

Page 1
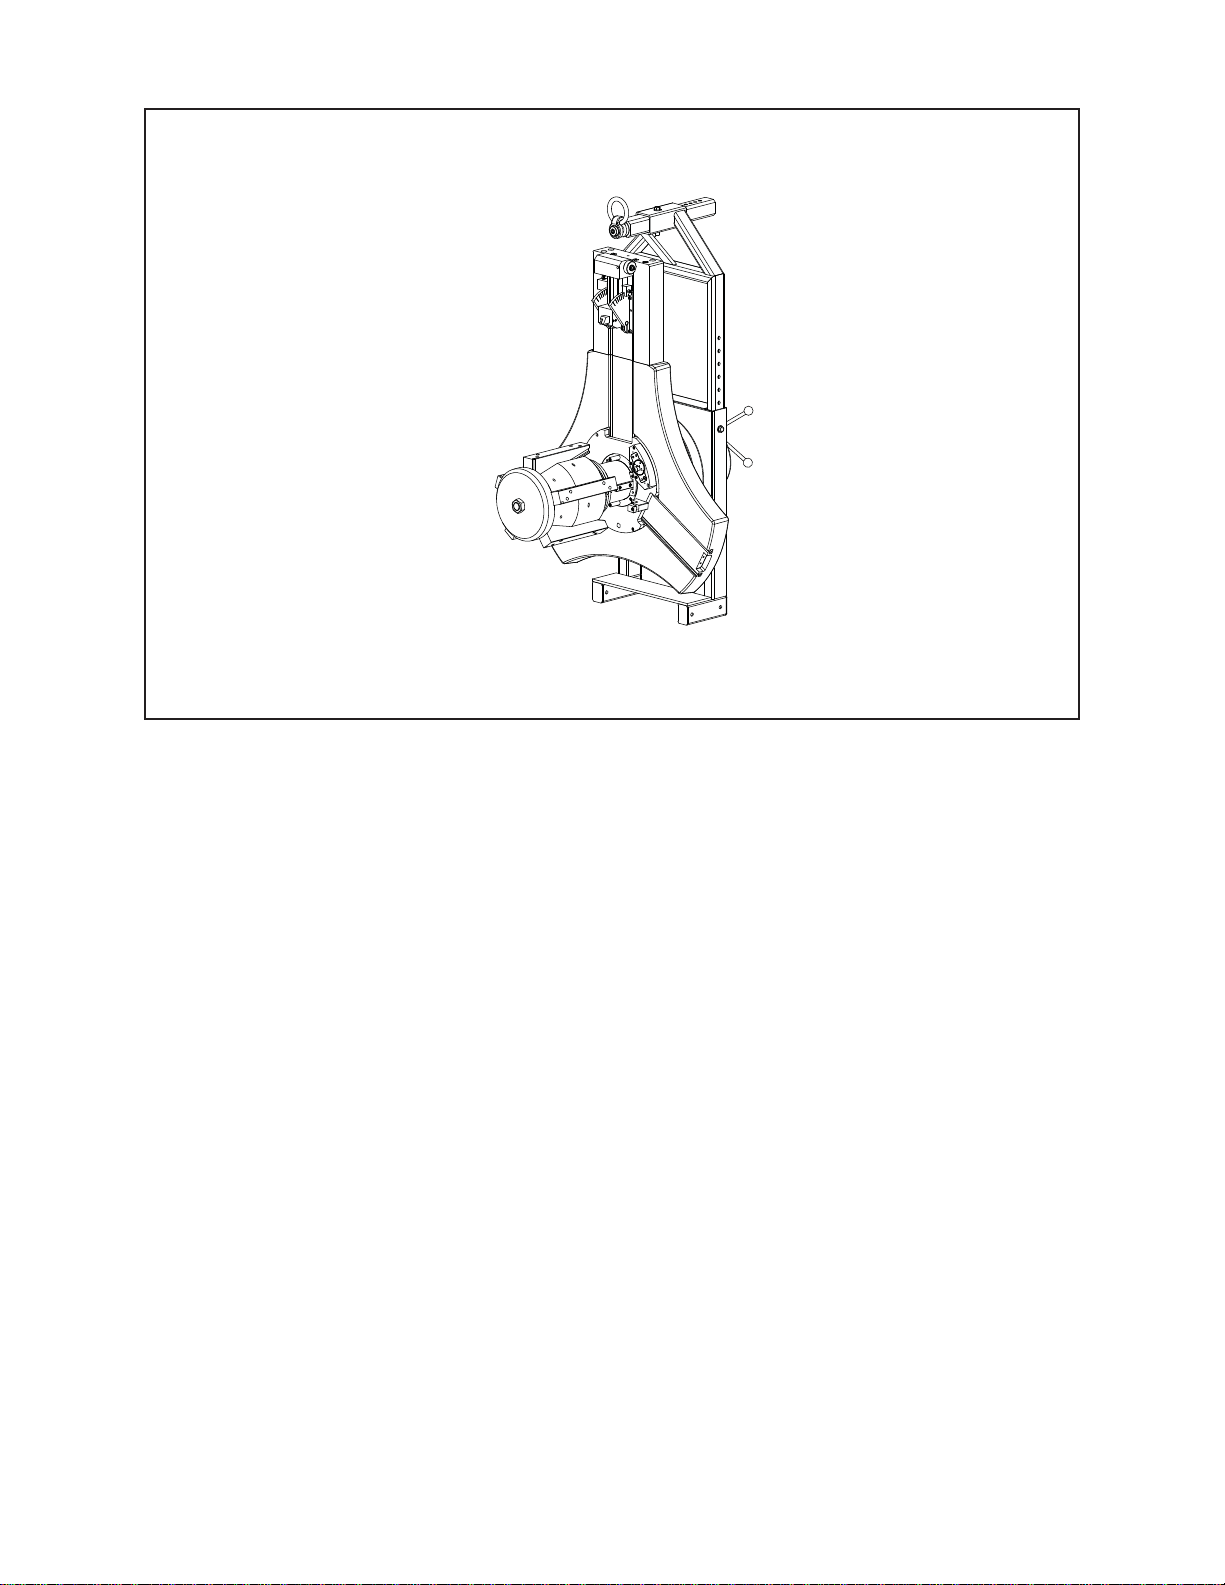
TABLE OF CONTENTS
CUSTOMER MESSAGE Inside Front Cover
SAFETY PRECAUTIONS 3
92-1333 Rev. 110404
Model 236B Single Point
GENERAL DESCRIPTION 6
SPECIFICATIONS 7
INST ALLATION 9
OPERA TION 1 1
CUTTING SPEEDS AND FEEDS 1 7
TOOL BITS 19
MAINTENANCE 20
SP ARE P ARTS 2 1
TROUBLE SHOOTING 22
ILLUSTRA TED P ARTS BREAKDOWN 2 4
TOOL BIT RESHARPENING POLICY Inside Back Cover
WARRANTY INFORMATION Inside Back Cover
Page 2
Copyright 2011
Proprietary property of TRI TOOL Inc.
No reproduction, use, or duplication of the
information shown hereon is permitted without the
express written consent of TRI TOOL Inc.
Page 3
SAFETY PRECAUTIONS
IN GENERAL
When using rotating head cutting equipment, basic safety precautions should always be followed to reduce the risk of personal injury .
Operate this tool only in accordance with specific operating instructions.
Do not override the deadman switch on the power unit. Locking down,
W ARNING:
DRESS CONSIDERA TIONS
obstructing, or in any way defeating the deadman switch on the power drive
unit may result in serious injury.
Model 236B Single Point
Use standard safety equipment. Hard hats, safety shoes, safety harnesses, protective clothes, and other safety devices should always be used when appropriate.
Use safety glasses. Do not operate cutting tools without eye protection.
Dress properly . Do not wear loose clothing or jewelry . They can be caught in rot ating and moving parts. Avoid slippery floors or wear nonskid footwear . If you have
long hair , wear protective hair covering to contain it.
WORK AREA
Keep the work area clean. Cluttered work areas and benches invite injuries.
Consider the work area environment. Keep the area well lit. Keep electrical cords,
cables, rags, rigging straps, and etc. clear of rotating equipment. Do not use
power-cutting tools in the presence of flammable liquids and gasses.
Keep visitors away . Do not let visitors or untrained personnel at or near operating
tools. Enforce eye protection requirements for all observers.
Do not over reach. Keep proper footing at all times.
St ay alert. Watch what you are doing. Use common sense. Do not operate tools
when you are tired.
92-1333 : Rev. 110404
3
Page 4
TRI TOOL INC.
TOOL CARE
Maintain tools with care. Keep tools in good operating condition. Sharp tool bits
perform better and safer than dull tool bits. Well maintained tools function properly
when needed.
Check for damaged parts. If a tool has malfunctioned, been dropped or hit, it must
be checked for damage. Run no-load tests and feed function checks. Do a complete visual inspection.
Electric motors. Use only with proper AC voltage power sources and observe all
normal electric shock hazard procedures.
Do not abuse power and control cords. Pulling or running over cords and cables
can result in electrical shock hazards and malfunctions. Keep control and power
cords out of all cutting fluids and water.
Hydraulic drives. Observe proper procedures for electrically driven power sources.
Avoid damage to hydraulic lines. Keep quick-disconnects clean. Grit contamination causes malfunctions.
Air tools. Check the exhaust muffler . Broken or damaged muf flers can restrict air
flow or cause excessive noise. Use air motors only with a filtered, lubricated and
regulated air supply . Dirty air , low-pressure air or over pressure air will cause
malfunctions, including delayed starting.
AREA EQUIPMENT
Secure work. Whenever possible use clamps, vises, chains and straps to secure
pipe.
Make sure the tool is secured; it is safer to have both hands free to operate the tool.
TOOL USE
Use the right tool and tool bit for the job. Do not use a tool, which is incorrect for the
job you are doing.
Keep the tool bits fully engaged in the tool bit holders. Loose bits are a safety
hazard.
4
92-1333 : Rev. 110404
Page 5
Model 236B Single Point
Disconnect the power supply during setup and maintenance. Use all 'Stop' or 'Shut
off' features available when changing or adjusting tool bits, maintaining the tool, or
when the tool is not in use.
Remove adjusting keys and wrenches before applying power to the equipment.
Develop a habit of checking the tool before turning it on to make sure that all keys
and wrenches have been removed.
Do not force tools. Tools and tool bits function better and safer when used at the
feed and speed rate for which they were designed.
Do not reach into rotating equipment. Do not reach into the rotating head stock to
clear chips, to make adjustments, or to check surface finish. A machine designed
to cut steel will not stop for a hand or an arm.
Handle chips with care. Chips have very sharp edges and are hot. Do not try to pull
chips apart with your hands; they are very tough.
Avoid unintentional starts. Do not carry or handle tools with your hand on the operating switches or levers. Do not lay the tool down in a manner that will start the
drive. Do not allow the tool to flip around or move when adjusting or changing tool
bits.
Store idle tools properly . Disconnect tools from the power source and store in a
safe place. Remove tool bits for safe handling of the tool.
92-1333 : Rev. 110404
5
Page 6
TRI TOOL INC.
GENERAL DESCRIPTION
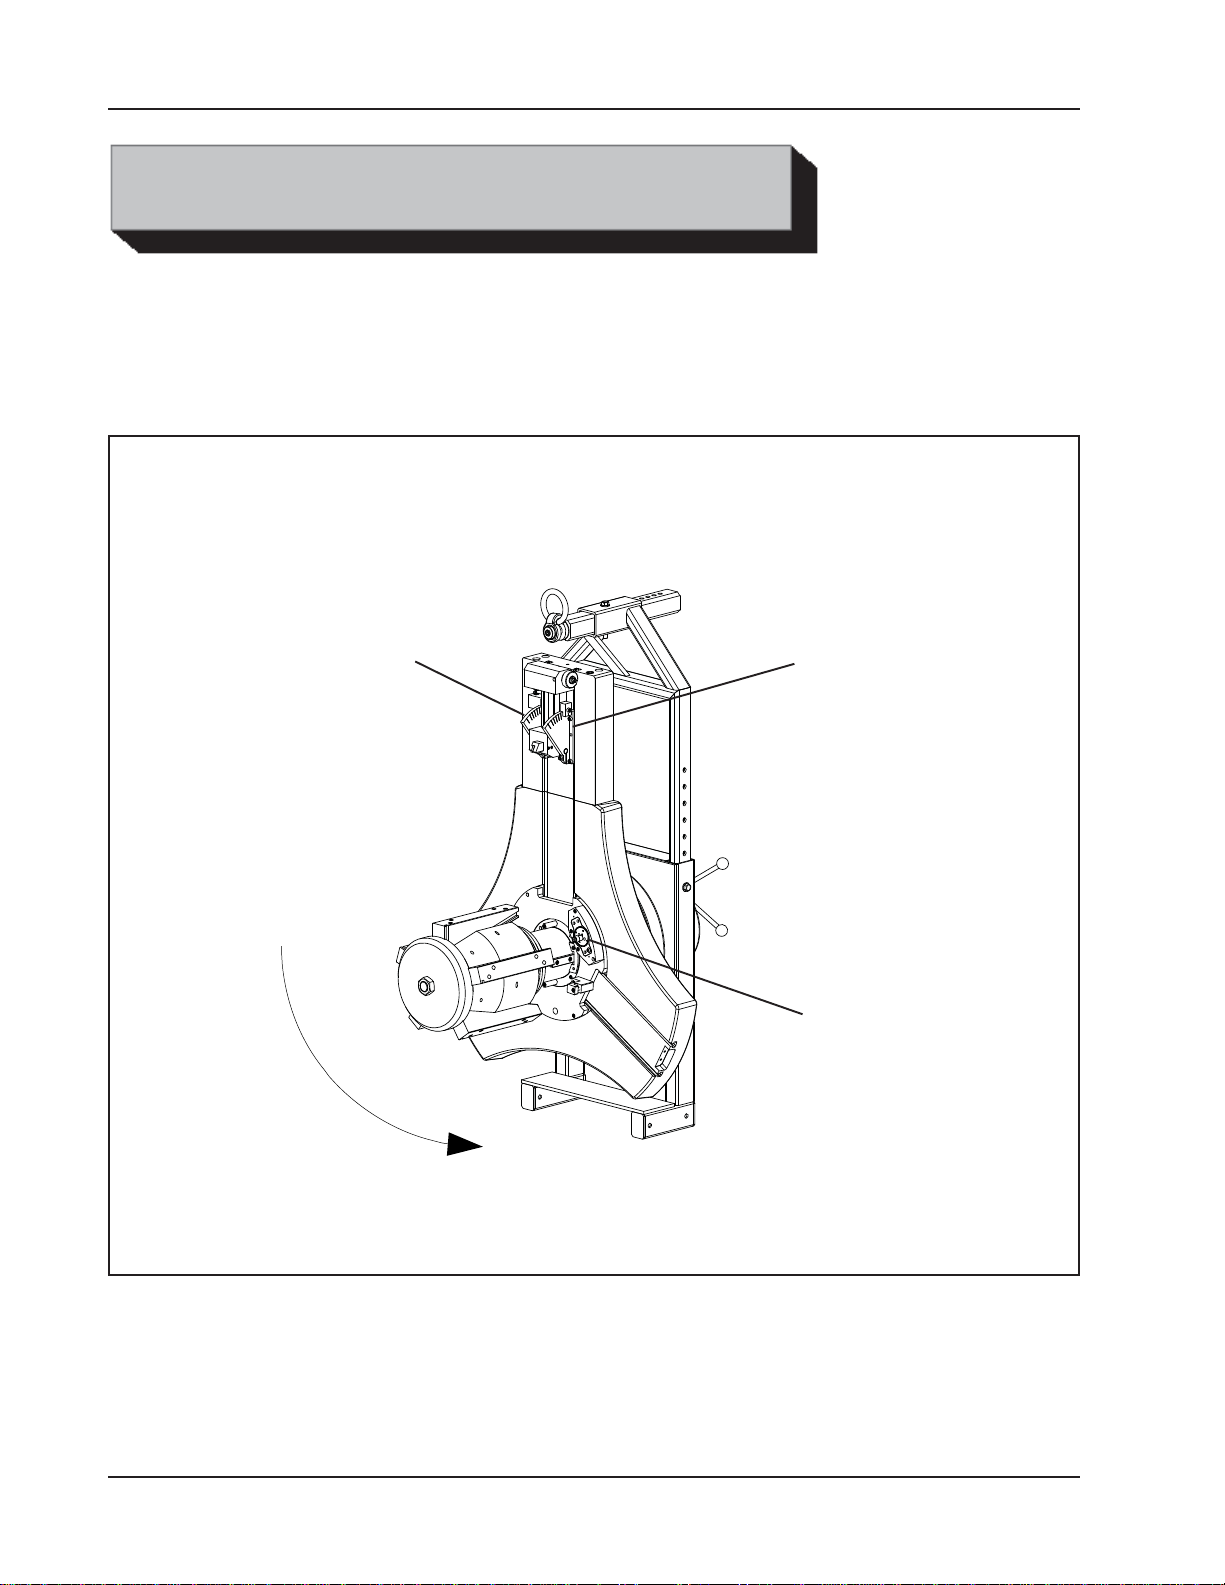
The Model 236B Single Point is supplied as a kit with modular components assembled onto the face of the 236B BEVELMASTER™. The 236B then mounts on
the flange or pipe I.D. When used in conjunction with the 236B Miter Mandrel, the
236B Single Point/Flange Facer Kit miters to align to the flange face.
General Nomenclature
Tilt Positioning
T ool Rotation
Manual Radial
Positioning
Autofeed
6
92-1333 : Rev. 110404
Page 7
SPECIFICATIONS
DESIGN AND OPERATING FEATURES
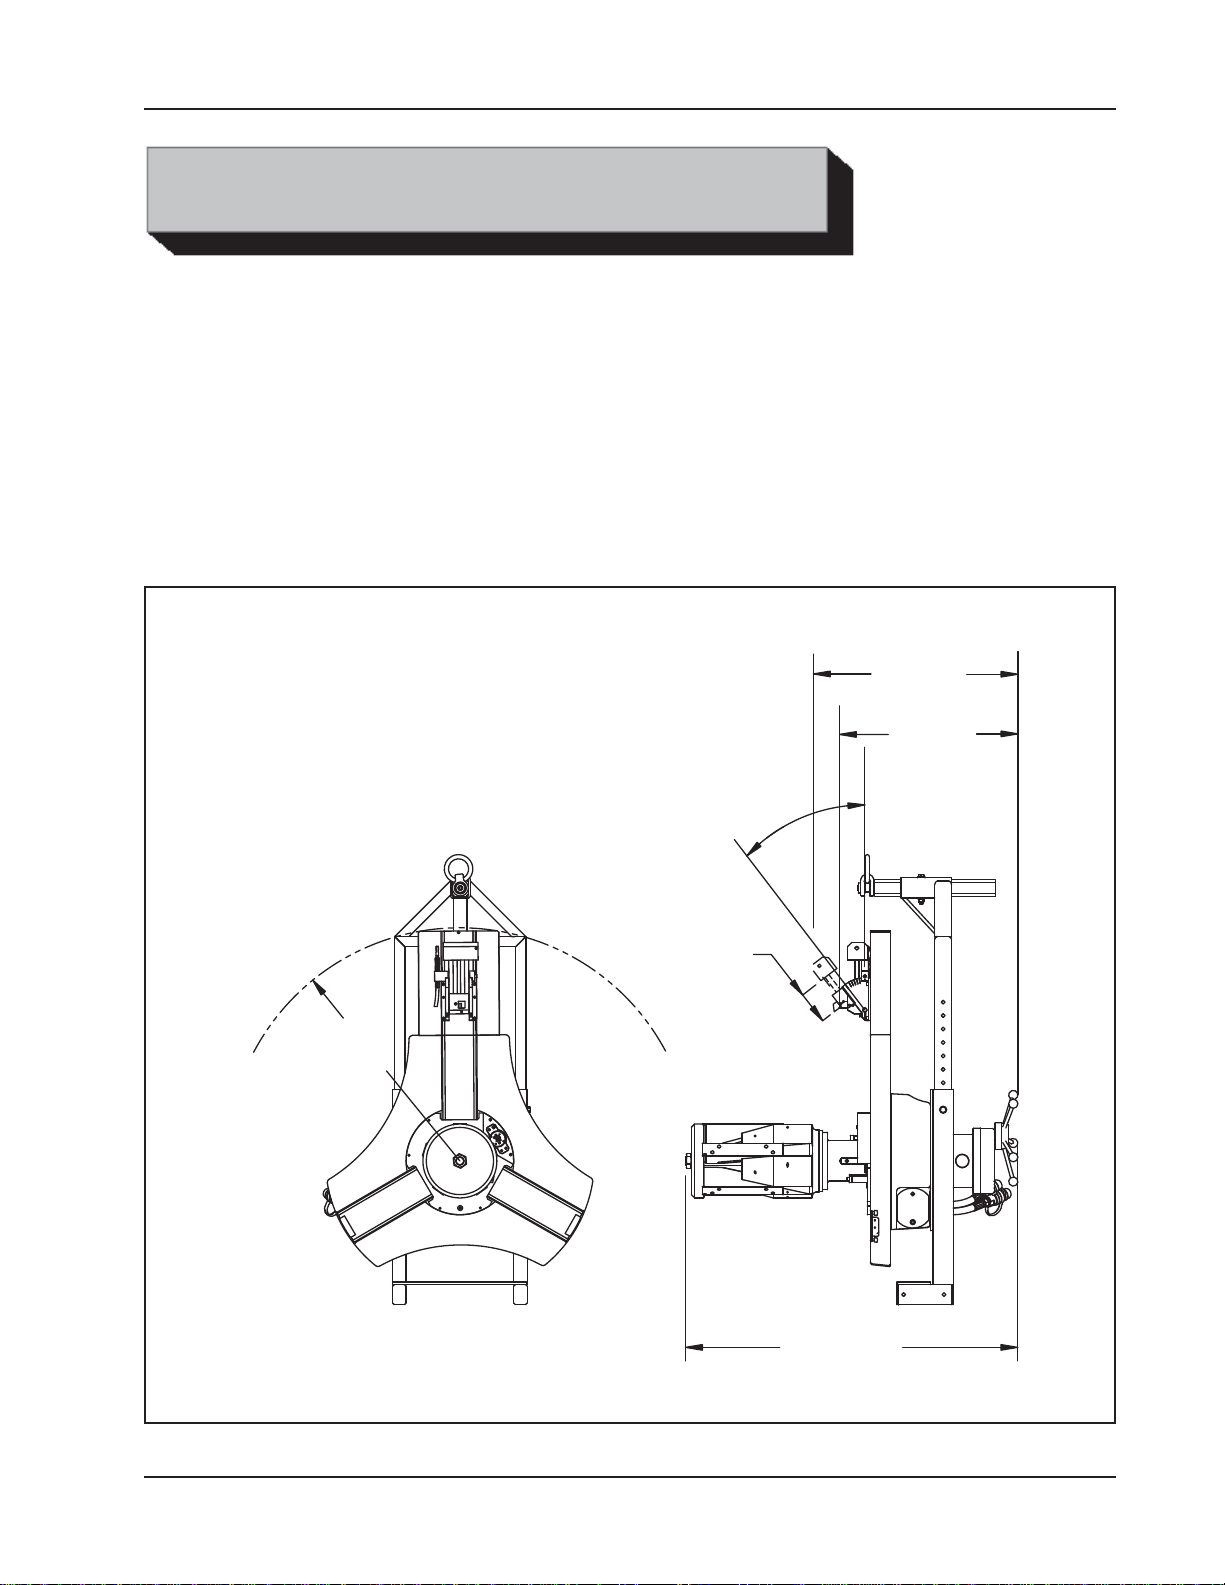
Easy to assemble 236B SP Kit bolts directly to the face of the 236B without any
modification to the machine.
The 236B SP is equipped with 5” (127.0 mm) of feed travel for heavy wall pipe and
flange facing with the miter mandrel kit.
The 236B SP has a travel range of 4" (101.6 mm) with the 5-jaw mandrel attached.
Envelope Drawing
Model 236B Single Point
31.41"
(797.8 mm)
26.62"
(676.1 mm)
78.40"
(1991.4 mm)
Max. Rotating DIA.
37 1/2°
5.00"
(127.0 mm)
Feed Travel
48.16"
(1223.3 mm)
92-1333 : Rev. 110404
7
Page 8
TRI TOOL INC.
The slide assembly has infinitely variable bevel angle adjustments between 0 and
37 1/2°.
The 236B SP has a total radial travel of 26.30” (668.0 mm) and adjustment for large
pipe and flange cutting ranges.
IN SPECIFIC
Range, Beveling 15.00" (381.0 mm) diameter to 60.00" (1524.0 mm)
Bevel Angles 0° to 37 1/2° graduated bevel angle adjustment.
Range, Flange Facing 20.00" (508.0 mm) diameter to 68.00" (1727.2 mm)
Feed Travel 5.0” (127.0 mm) nominal (radial).
diameter cutting range at 37 1/2°
diameter cutting range.
Alignment When used in conjunction with the 236B Miter
Mandrel Head:
Angular - ± 5°
Off set - ± .19” (4.83 mm)
Feed Eight (8) selectable positions between .006”
(.152 mm) rev . and .042” (1.07 mm) rev . inclusive
Cutting: .200 max. cut depth/pass.
63 RMS finish may be obtained depending on
material.
Spiral grooves as coarse as 31 grooves per inch
when grooving.
Machines stainless and carbon.
8
92-1333 : Rev. 110404
Page 9
Model 236B Single Point
INSTALLATION
ATT ACHING THE MODEL 236B SP KIT TO THE MODEL 236B
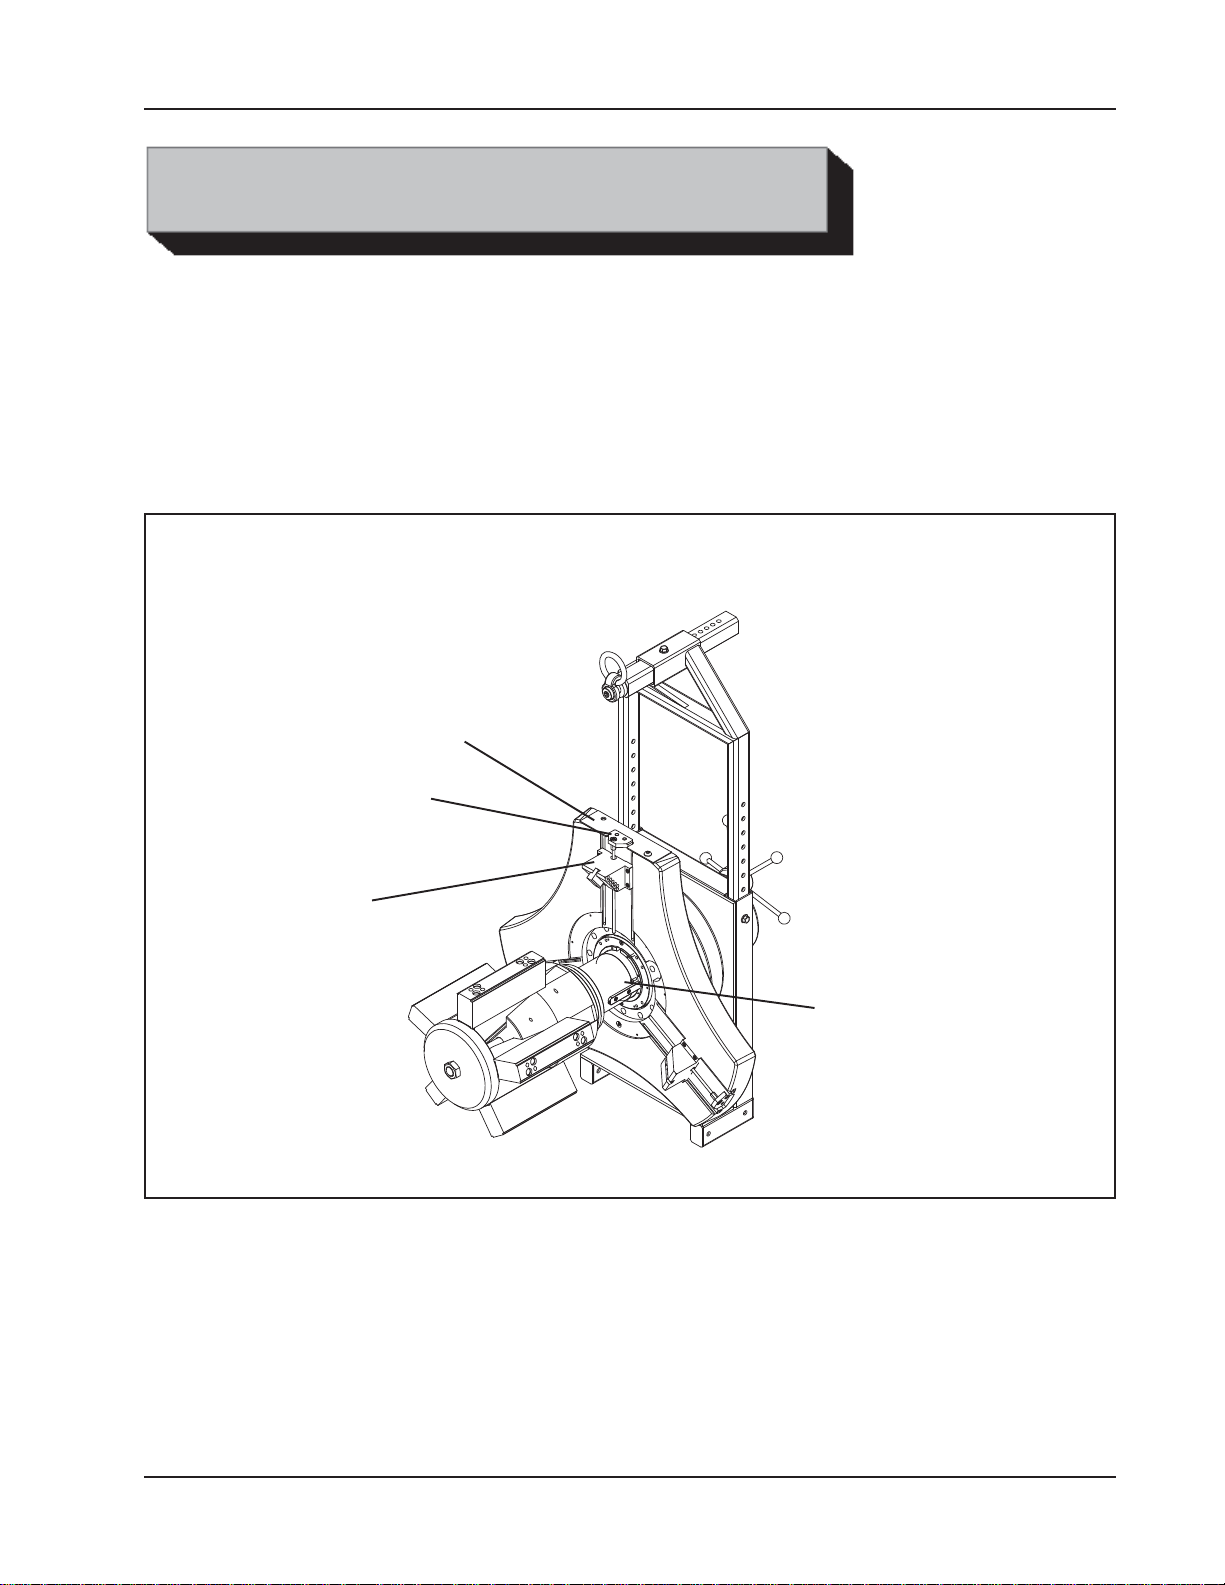
Remove the Mandrel Assembly , T ool Holder Assembly , Adjustment Rod Assembly
and the Cover Plate from the Model 236B Machine.
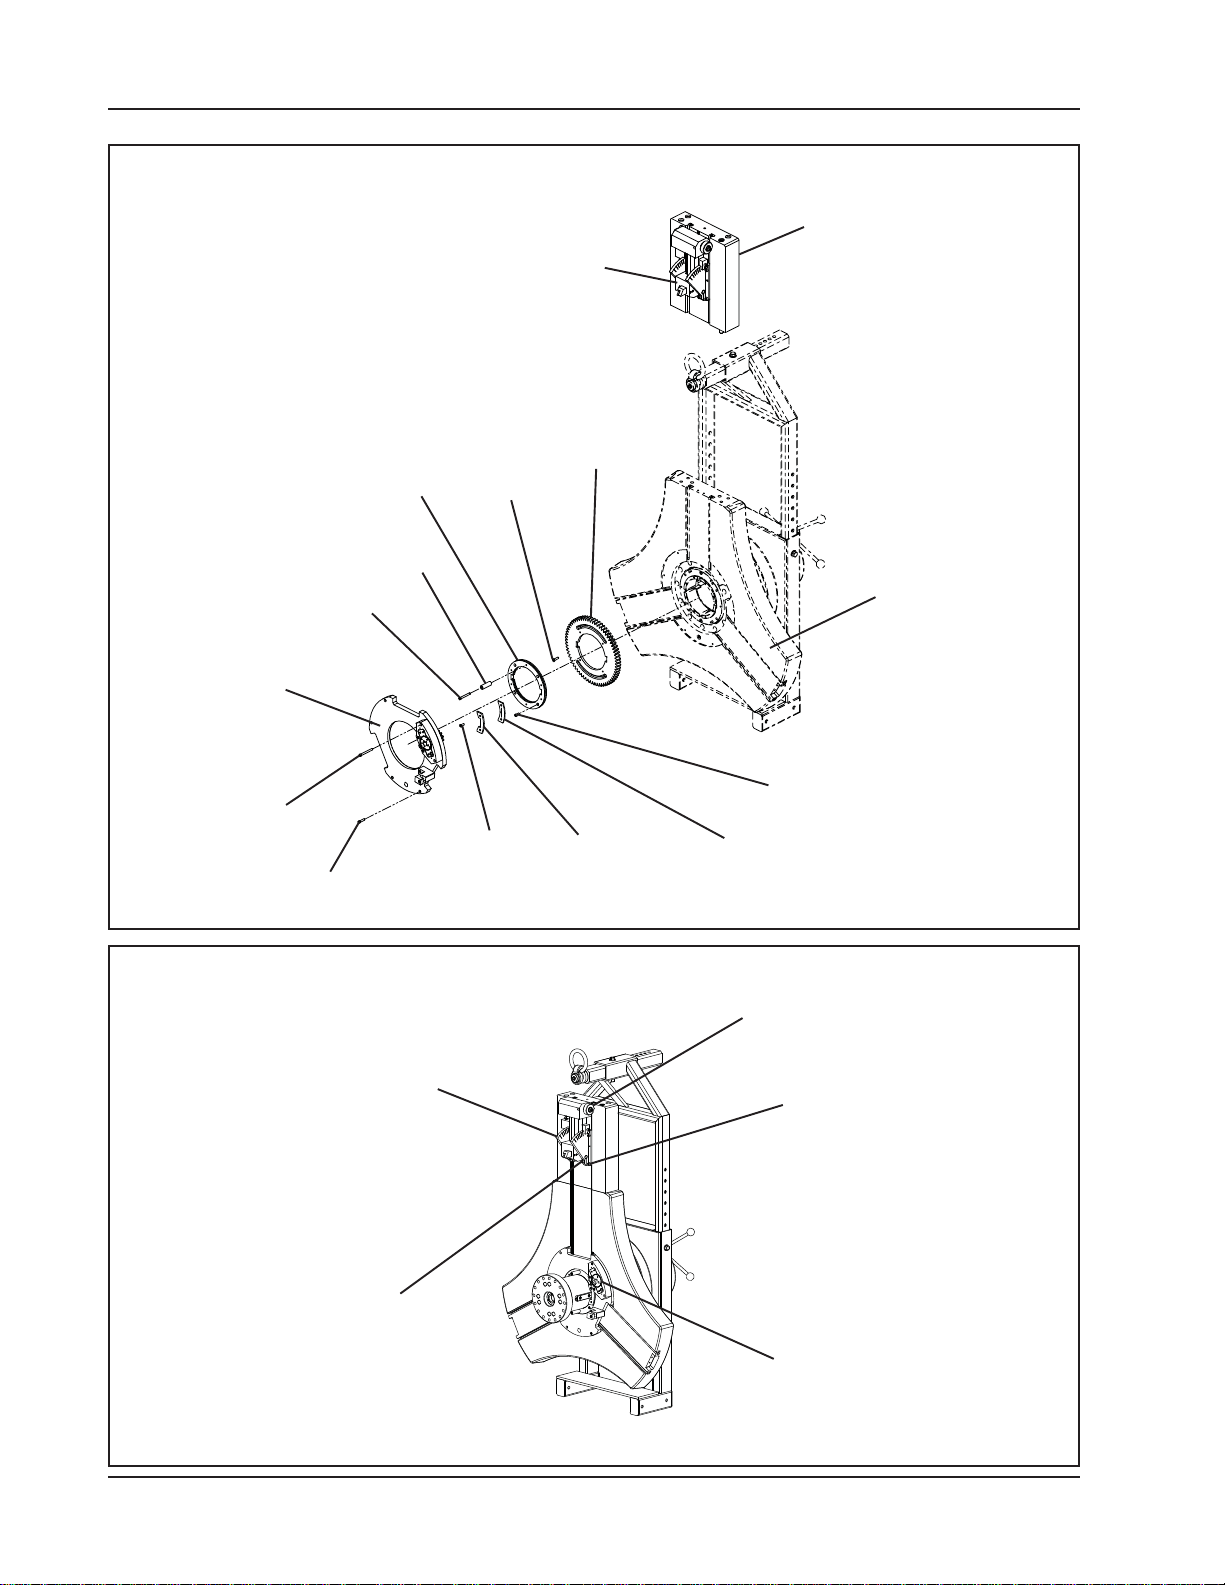
Secure the Gear (P/N 39-1 102) to the Front Locking Plate using supplied flat head
screws (P/N 33-0362).
T ool Configuration prior to Single Point installation
Cover Plate
Adjustment Rod
Assembly
T ool Holder
Assembly
Mandrel Assembly
Secure the Feed Gear Housing Assembly (P/N 82-0226) to the Main Plate, using
supplied cap screws (P/N 33-0043).
Install Plate Assembly , Adapter (P/N 24-2707) onto Main Plate (flat), secure in place
with retained cap screws.
Slide the Cutter Assembly into T -slots on Adapter Plate Assembly to position desired and secure the six (6) cap screws on the base.
92-1333 : Rev. 110404
9
Page 10
TRI TOOL INC.
Installation of the 236B Single Point
Cutter Assembly
Adapter Plate
Assembly
Gear Cover
Assembly
Stop Block
Cap Screw
Feed Gear
Housing
Assembly
Cap Screw
Cap Screw
Various Adjustment Locations
Dovetail Slide
Lock Screw
Flat Screw
Button
Screw
Gear
Mandrel
Seal
Main Plate
Cap Screw
Key Wiper
Mandrel Seal
Manual Directional
Feed Knob
Radial Adjustment
Screws (6)
10
Angular Adjustment
Screw (both sides)
Index Plate
92-1333 : Rev. 110404
Page 11
WARNING:
PINCH POINT - Remove the Lathe Stand Feet Supports BEFORE
operating.
Page 12
TRI TOOL INC.
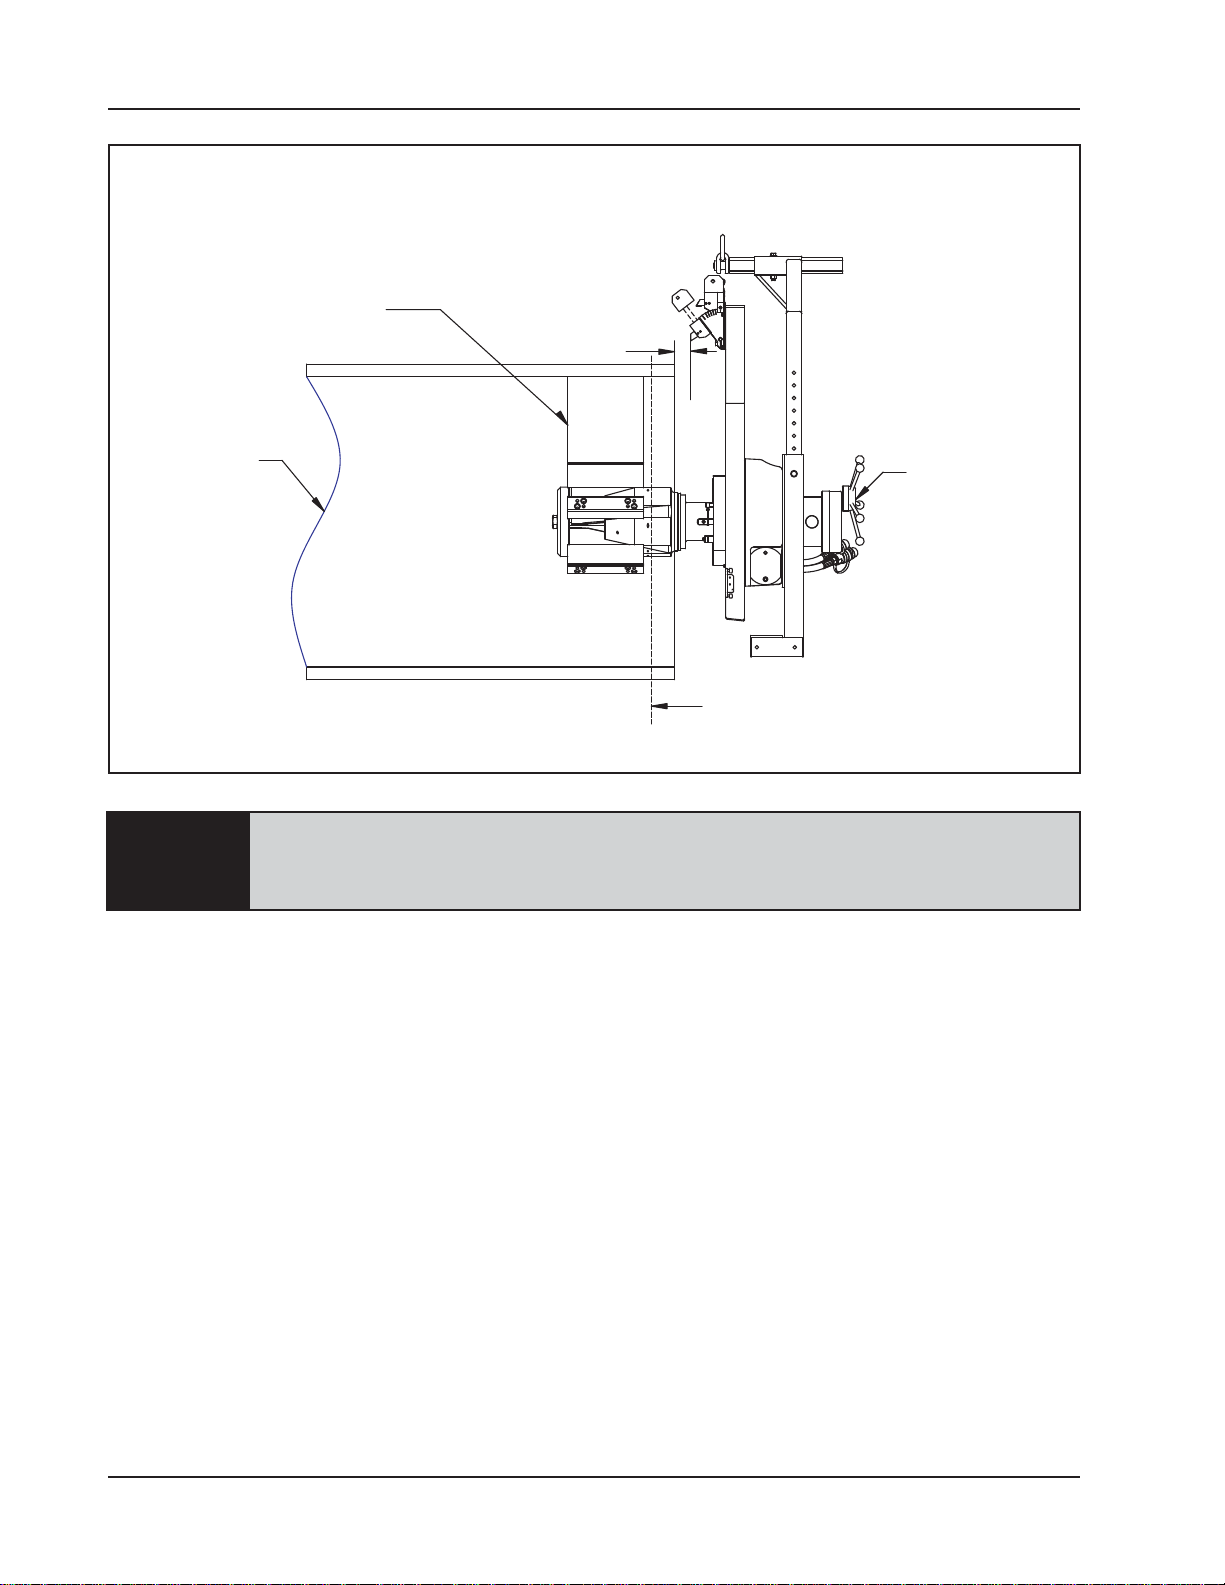
Tool Bit Clearance
Jaw Block
Clearance
NOTE:
Pipe
Final Prep Location
Attach the proper power supply line to the drive assembly. If using a pneumatic drive assembly, use an adequate in-line filter, regulator, and lubricator (FRL).
The Tri T ool Air Caddy , a portable combination filter, regulator, and lubricator
(FRL) unit is recommended.
Feed
Handle
Plate
12
Turn the motor on.
Let the machine rotate very slowly for one revolution to verify that the tool bit clears
the OD of the pipe.
Adjust the cutting speed by opening the Flow Control V alve at the power supply
connection.
The actual machining operation will begin when the tool bit contacts the pipe.
If the pipe end is not square with the pipe axis, the tool bit will contact only a
small segment of the pipe during each revolution.
92-1333 : Rev. 110404
Page 13
Remove the machine from the pipe.
Check to see if any of the tool bits are dull or broken.
Damaged or worn tool bits are evident by increased feed pressure, visual
observation, poor surface finish, etc.
When the next bevel is going to be the same end preparation as the previous bevel,
install the machine and mandrel in the pipe and follow the same sequence of steps
that was used to completed the bevel.
When the next bevel is going to be different than the previous bevel, follow the
sequence in 'Adjustment of the Tool Block Assembly' section.
For changing the tool bit, follow the sequence in the 'Counter Boring Function'
section.
ADJUSTMENT OF THE TOOL BLOCK ASSEMBLY
Model 236B Single Point
While holding the tool block slide assembly , loosen the six (6) screws on the base
of the slide.
Reposition the slide assembly and tighten the six (6) screws. This will hold the slide
firmly against the plate.
T o adjust the bevel angle of the slide, loosen the locking screws on the sides of the
slide, pull the slide up to the required angle and tighten the screws, maximum angle
is 37° 30’.
INST ALLATION OF THE TOOL HOLDER AND INSERT
T o select the appropriate tool holder and Insert, reference the 'Tooling' section of
this manual.
Use of a dull Insert or Inserts not manufactured by T ri Tool Inc. may result in poor
performance and may constitute abuse of this machine and therefore voids the T ri
T ool Inc. factory warranty .
Slide the assembled tool holder with Insert into the tool holder slot on the tool block.
Install the tool holder with the Insert with the cutting edge toward the mandrel .
Lock the tool holder into position with the set screws on the side of the tool holder .
92-1333 : Rev. 110404
13
Page 14
TRI TOOL INC.
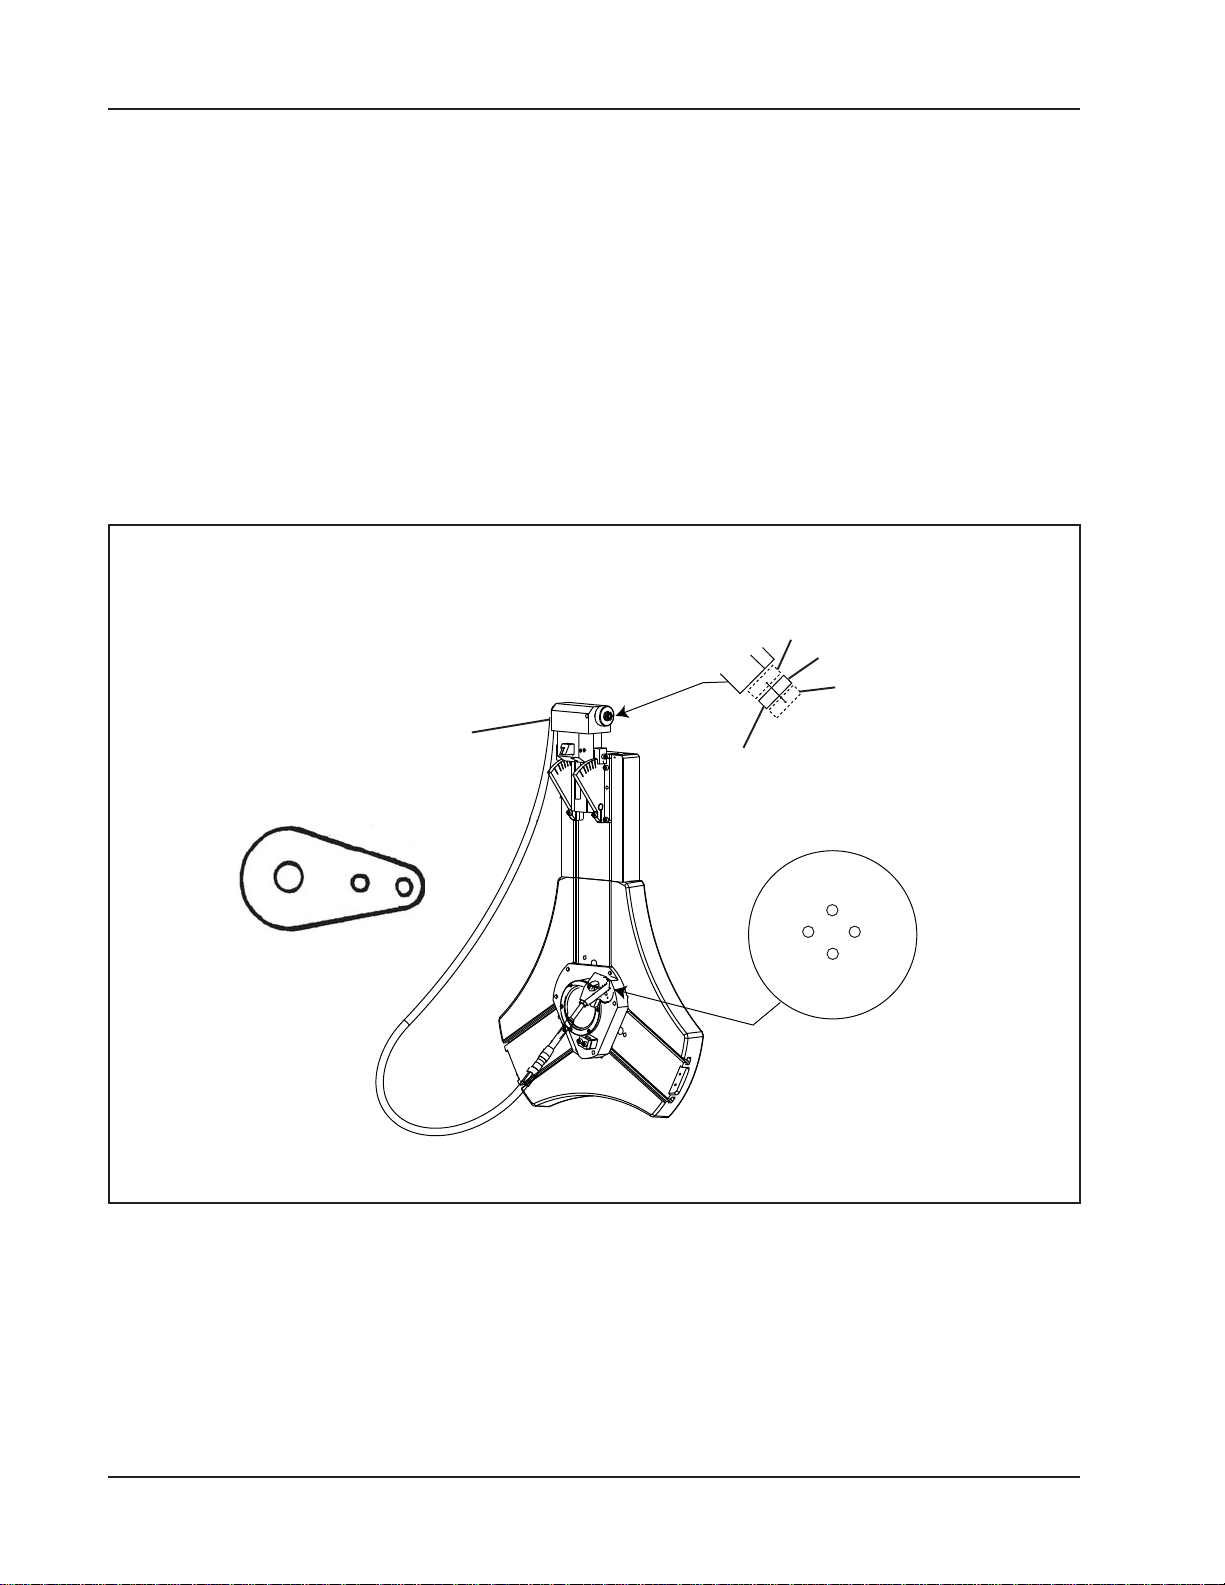
FEED ADJUSTMENT
Put the gearbox into neutral.
SETTING THE FEED DIRECTION
Select the proper hole location on the position index plate and the actuator arm for
the required feed.
Set the feed direction by pulling out the knob (for feeding toward the mandrel), in
the center position (for neutral or no feed) or by pushing in the knob (for feeding
away from the mandrel).
Feed System Set-Up
Feed Out
Neutral
Feed In
Actuator Arm
B
A
COUNTERBORING FUNCTION
Feed Knob
1
3
2
4
Index Plate
14
Lock the tool slide in the flat position.
Replace the tool holder and the Insert with the counterbore tool bit.
Insure that the cutting edge is facing out from the center.
92-1333 : Rev. 110404
Page 15
Model 236B Single Point
Set the feed direction to neutral by moving the feed knob to the center position.
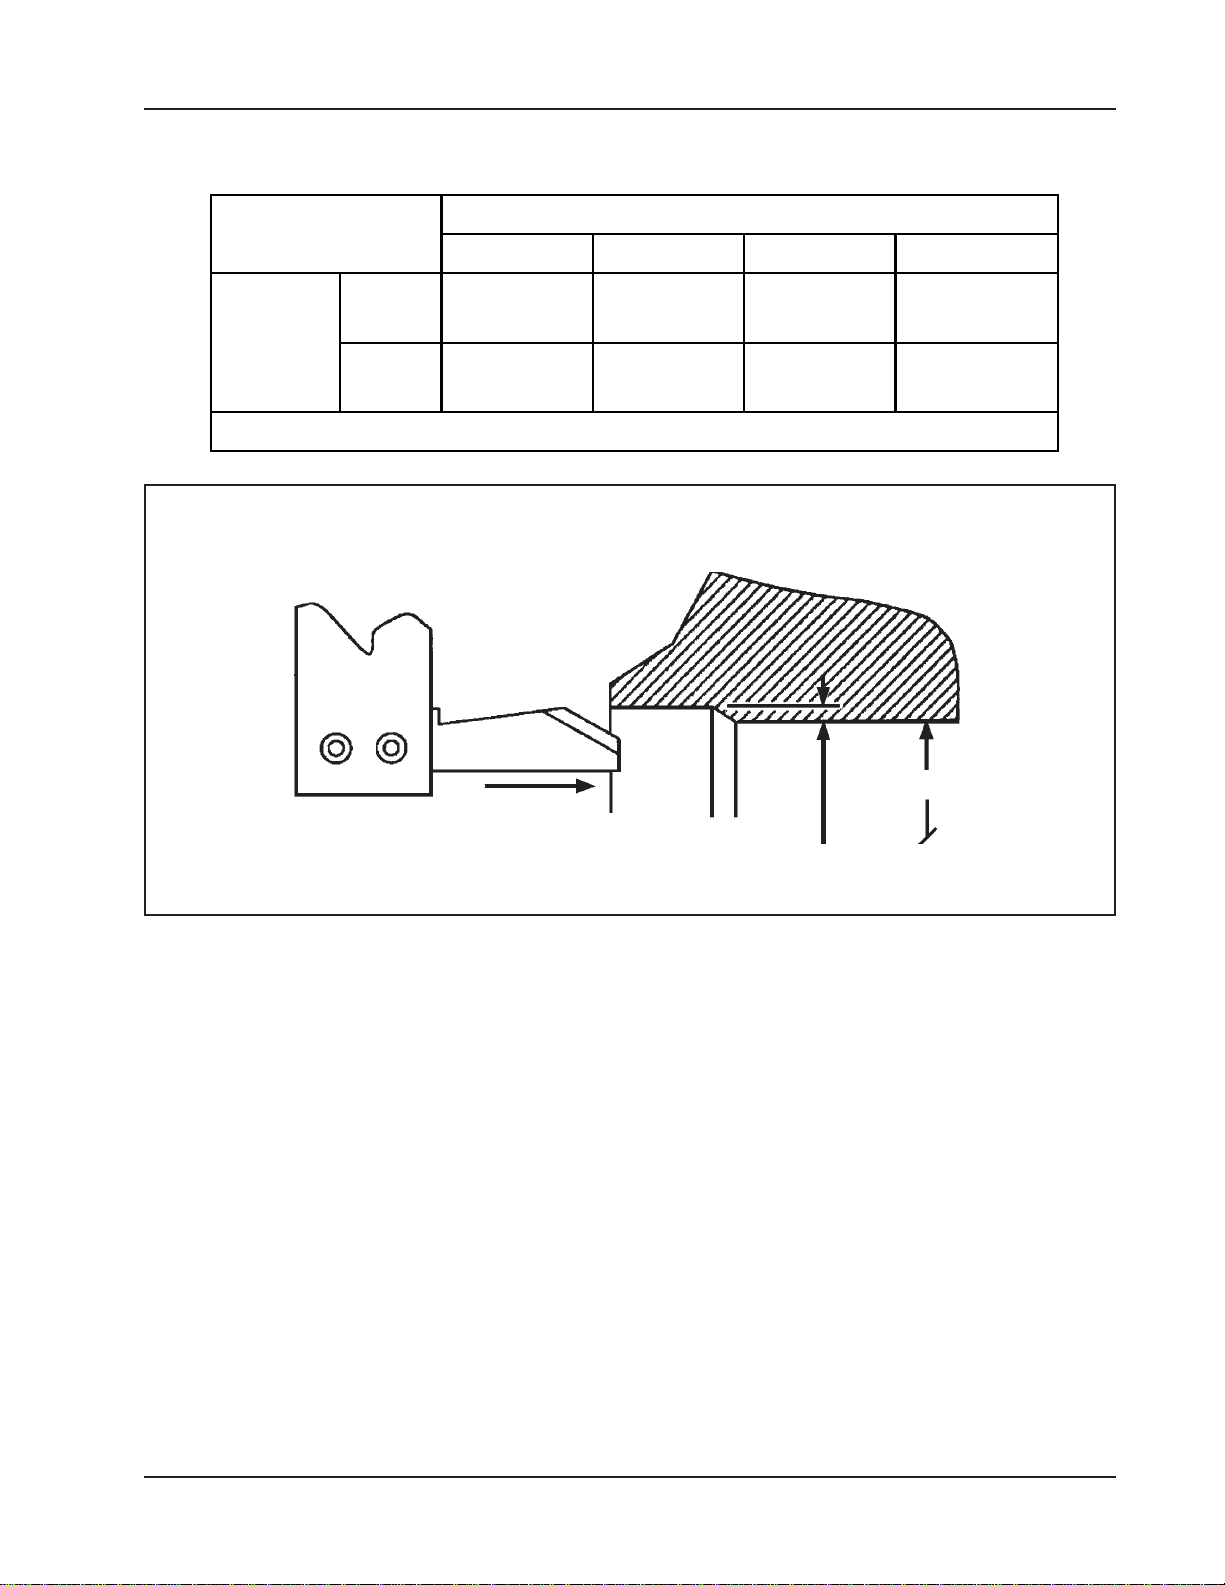
INDEX PLATE POSITIONS
1 2 3 4
Actuator
A
.004"/rev
(.101 mm/rev)
.007"/rev
(.178 mm/rev)
Arm
Position
B*
.006"/rev
(.152 mm/rev)
.011"/rev
(.279 mm/rev)
*Posittion B should be used for flange facing only.
Feed in of a Counterbore Tool Bit
.010"/rev
(.254 mm/rev)
.015"/rev
(.381 mm/rev)
.013"/rev
(.330 mm/rev)
.018"/rev
(.457 mm/rev)
Install the mandrel inside the pipe and tighten the draw nut to force the jaw blocks
out against the inside diameter of the pipe.
In order to avoid cutting the jaw blocks during the machining operation, the
mandrel must be installed beyond the final end preparation location.
Advance the machine by turning the feed knob clockwise until the tool bit is slightly
inside the pipe.
Move the tool slide out until the tool bit contacts the ID of the pipe and tighten the
slide.
Turn the manual feed knob on the tool slide so that the tool bit clears the bore ID
and back the machine out of the pipe.
Securely lock the tool slide in position by tightening all six (6) of the radial adjust
screws on the slide assembly.
92-1333 : Rev. 110404
15
Page 16
TRI TOOL INC.
Turn the motor on.
Let the machine rotate very slowly for one revolution to verify that the tool bit clears
the ID of the pipe.
Adjust the tool bit into the cutting position, use the manual feed knob on the tool
slide.
Tighten the dovetail slide lock screw in the tool block when desired tool bit position
has been achieved.
This screw must be loosened and re-tightened whenever the dovetail slide
requires repositioning.
When it is not securely tightened, the tool bit may walk out of the cut.
Plunge cut to desired depth.
16
92-1333 : Rev. 110404
Page 17
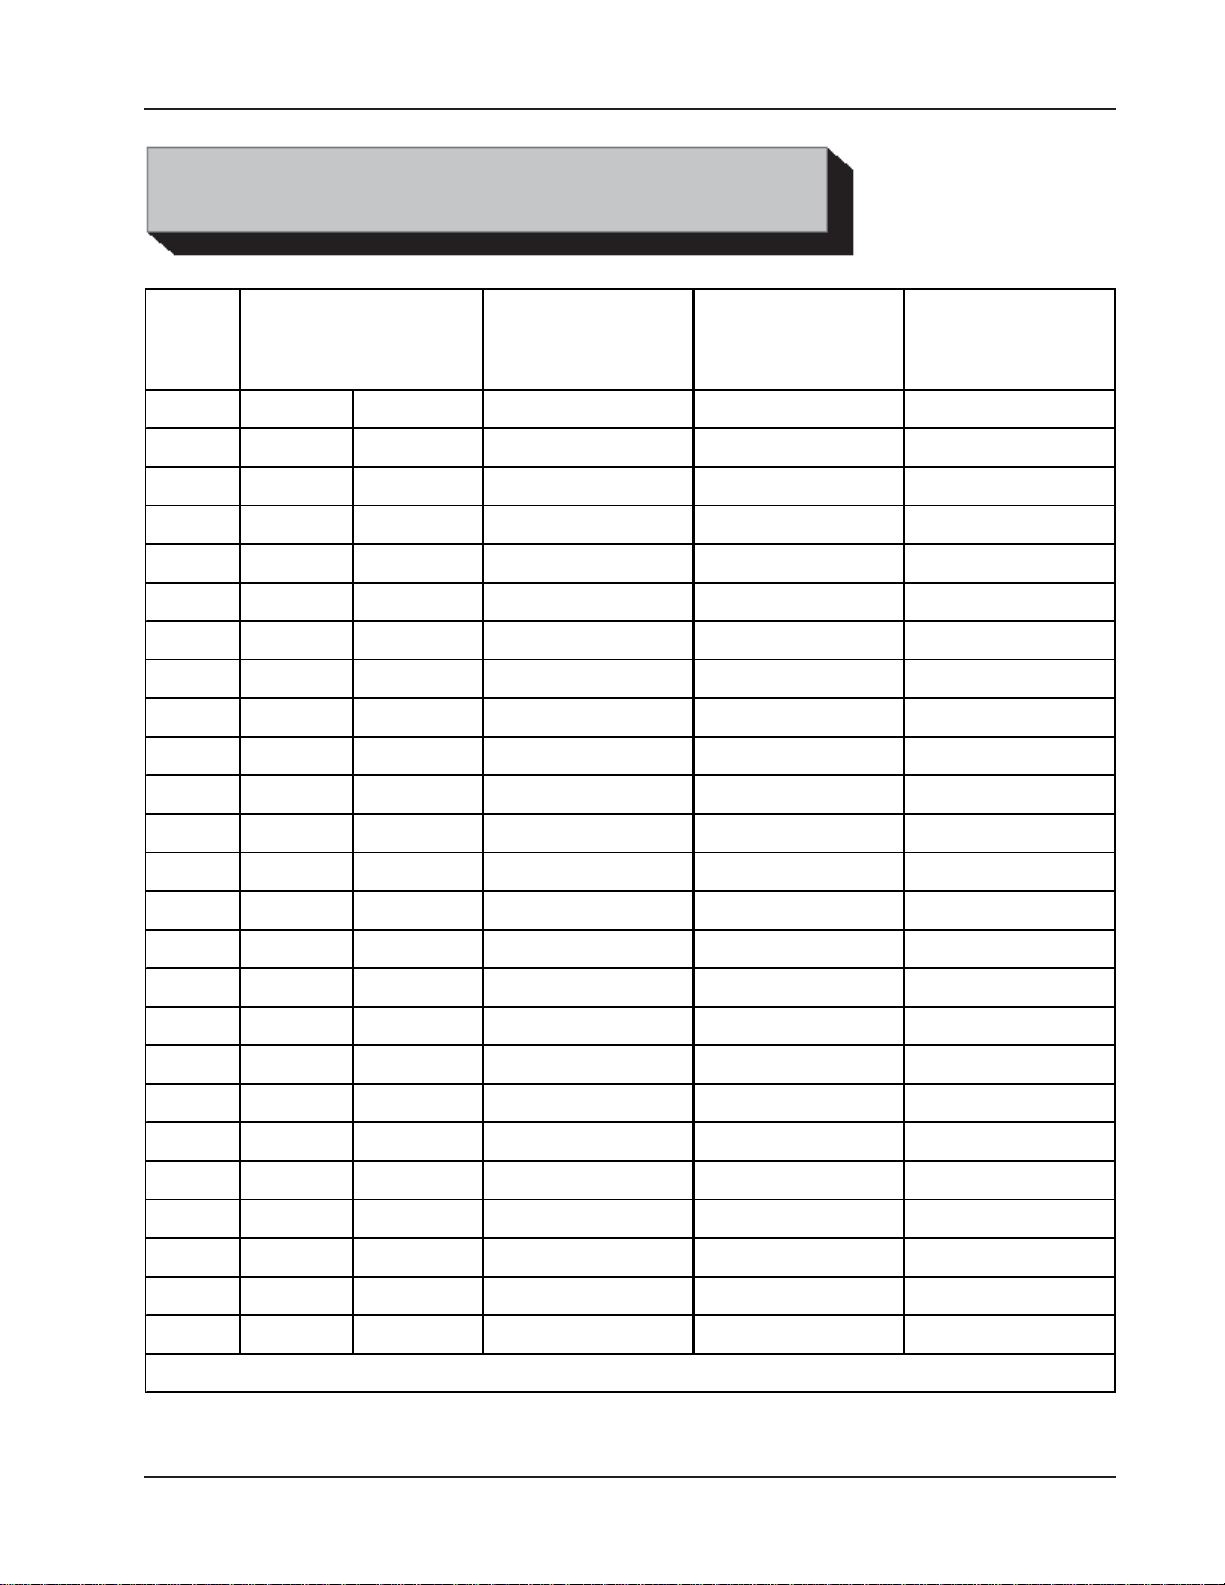
CUTTING SPEEDS AND FEEDS
Model 236B Single Point
Pipe
Size
62 62.00" 1574.8 mm 2 2 2
60 60.00" 1524.0 mm 2 2 2
58 58.00" 1473.2 mm 2 2 2
56 56.00" 1422.4 mm 2 2 2
54 54.00" 1371.6 mm 2 2 2
52 52.00" 1320.8 mm 2 2 2
50 50.00" 1270.0 mm 2 2 2
48 48.00" 1219.2 mm 2 2 2
46 46.00" 1168.4 mm 2 2 2
44 44.00" 1117.6 mm 2 2 2
42 42.00" 1067.0 mm 2 2 2
40 40.00" 1016.0 mm 2 2 2
38 38.0 0" 965.0 mm 2 2 3
True DIA
RPM for
200 in/min
(5080 mm/min)
RPM for
250 in/min
(6350 mm/min)
RPM for
300 in/min
(7620 mm/min)
36 36.0 0" 914.0 mm 2 2 3
34 34.0 0" 854.0 mm 2 2 3
32 32.0 0" 813.0 mm 2 2 3
30 30.0 0" 762.0 mm 2 3 3
28 28.0 0" 711.0 mm 2 3 3
26 26.0 0" 660.0 mm 2 3 4
24 24.0 0" 610.0 mm 3 3 4
22 22.0 0" 559.0 mm 3 4 4
20 20.0 0" 508.0 mm 3 4 5
18 18.0 0" 457.2 mm 4 4 5
16 16.0 0" 406.4 mm 4 5 6
15 15.0 0" 381.0 mm 5 6 7
Cutting Speed (approximately)
92-1333 : Rev. 110404
17
Page 18
TRI TOOL INC.
Use 200 surface inches per minute (5080 surface millimeters per minute) for:
Stainless steels in general when no coolant is allowed, all heavy-wall tube
and some chrome/molybdenum steels.
Use 250 surface inches per minute (6350 surface millimeters per minute) for:
Mild steels and some thin-wall stainless steels when coolants are permitted
and applied.
Use 300 surface inches per minute (7620 surface millimeters per minute) for:
Aluminum and some thin-wall mild steel and tube with coolants.
BASIC FEED RECOMMENDA TION
Use very light feed for initial beveling or until a continuous cut is established.
This is very important for longer tool bit life when cutting through flame cut or
out of square pipe ends.
Use adequate feed, .003” (.08 mm) to .006” (.15 mm) per revolution thereafter, to
establish a continuous chip cut.
If the feed is too light, only light stringer chips will be removed.
If the feed is too heavy the drive will start to overload and the chip will start to
have a rough or torn appearance.
Stainless steel, which work hardens, must be worked with a heavy enough feed to
stay under the work hardened surface .003” (.08 mm) to .006” (.15 mm) feed. Never
allow the tool bit to burnish the surface.
Reduced feeds and speeds will normally minimize chatter problems.
18
92-1333 : Rev. 110404
Page 19
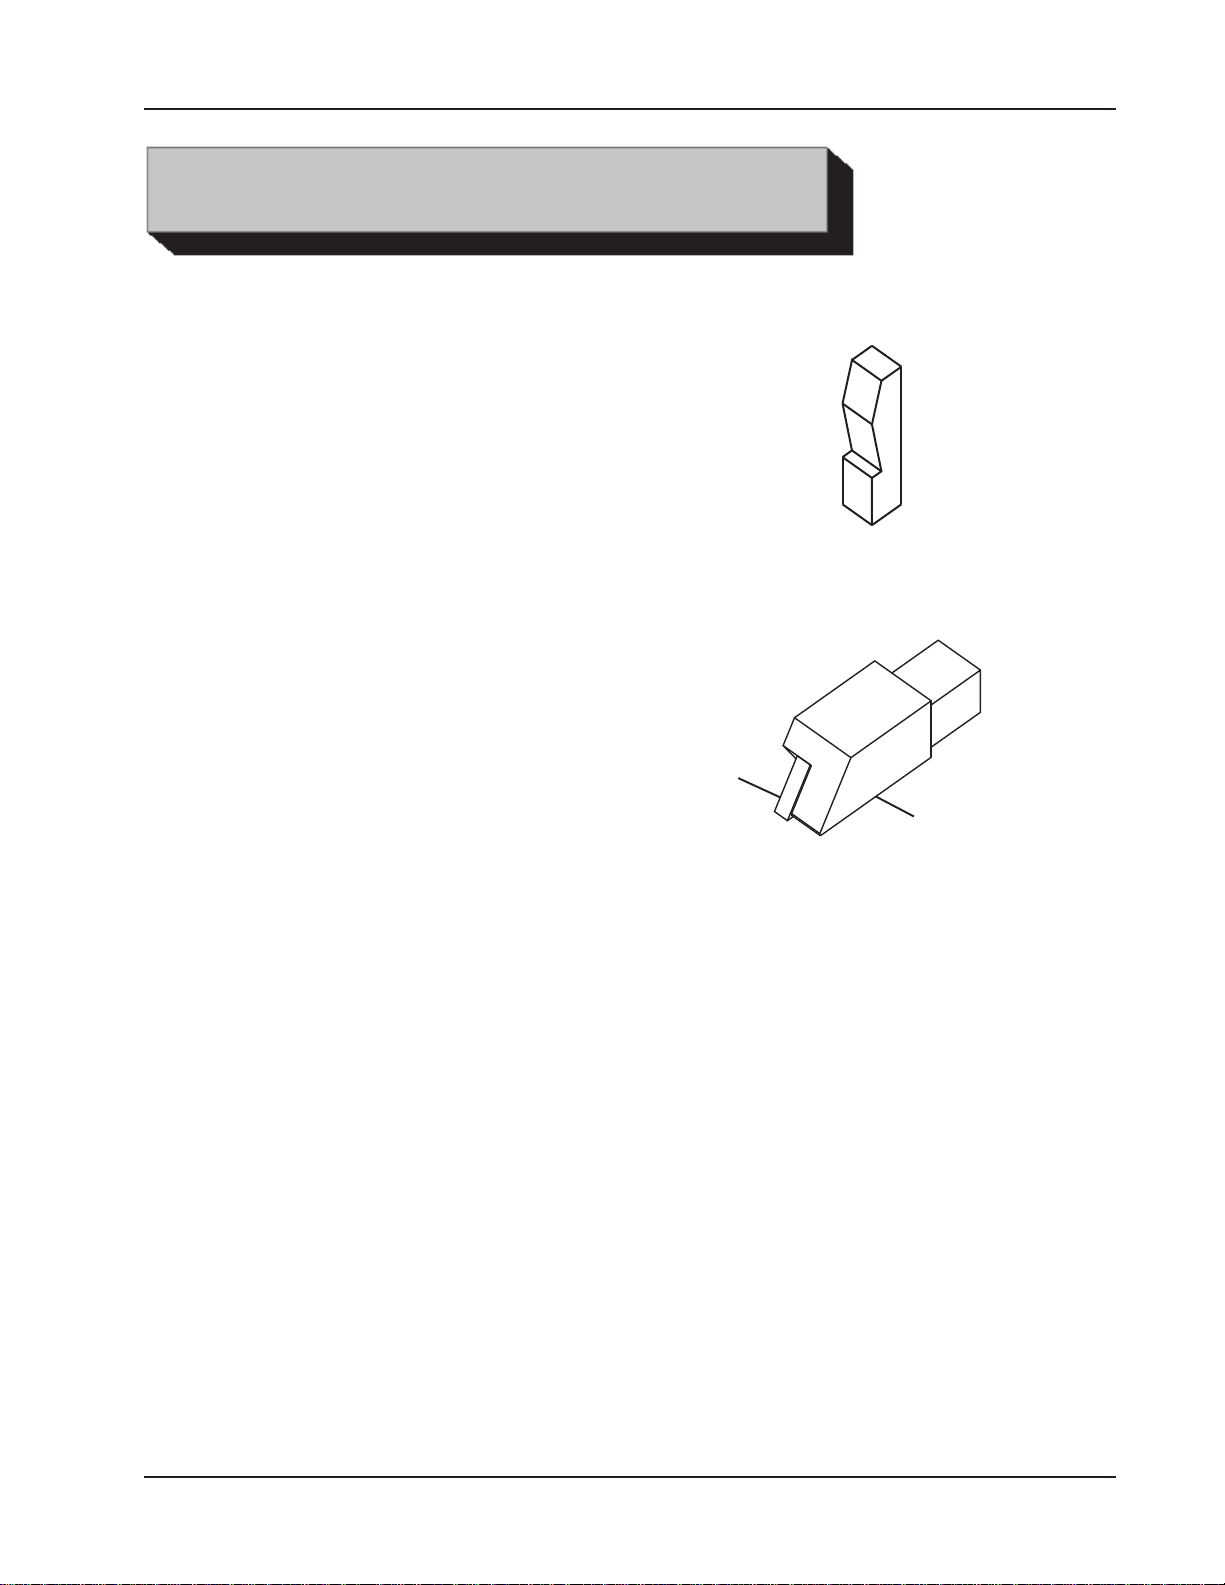
TOOL BITS
Tool Bit, Counterbore
(P/N 99-1666)
A) Insert, Triangular, .030 R
Model 236B Single Point
(P/N 30-0554)
A) Insert, Triangular, .015 R
(P/N 30-2822)
B) Tool Holder
(P/N 49-0060)
A
B
92-1333 : Rev. 110404
19
Page 20
TRI TOOL INC.
All components should be cleaned and coated with a light film of oil prior to use.
Daily maintenance should include a visual inspection of all parts for damage due to
chips, impact or improper use.
Repair or replace broken or damaged parts as necessary.
Wipe the machine clean of cutting fluids, dirt and grime and then coat it with a light
film of oil.
For complete weekly maintenance procedures, see the Model 236B
BEVELMASTER™ manual.
MAINTENANCE
20
92-1333 : Rev. 110404
Page 21
Model 236B Single Point
SPARE PARTS
Parts List, Recommended Spare Parts
Item Part
No. No. Description Qty
1. 29-0219 CAM FOLLOWER 1
2. 30-0554 INSERT, TOOL, .030 R 10
3. 30-2822 INSERT, TOOL, .015 R 10
4. 33-0955 SCREW , GIB 1
5. 35-0270 NUT, FEED 1
6. 49-0060 TOOL, HOLDER 1
7. 66-0079 GIB, TAPERED 1
92-1333 : Rev. 110404
21
Page 22
TRI TOOL INC.
TROUBLE SHOOTING
Problem: The T ool Bit Chatters
The tool bit is loose or overextended.
The tool bit is damaged.
The tool holder is too loose in the slides.
The cutting speed is too fast.
The clamping pads are loose on the pipe or tube.
Cutting fluid is required.
The main bearing pre-load is loose.
Problem: There's Excessive T ool Bit Wear
The pipe or tube material is too hard or abrasive.
The cutting speed is too fast.
Cutting fluid is required.
A dull Tool Bit is causing surface hardening conditions (Stainless pipe or
tubing).
There is scale or other foreign matter on the pipe or tube, which is dulling the
tool bit at the start of the cut.
The tool bit is incorrect for the material being cut.
Problem: The Surface Finish is Rough
The tool bit is dull, chipped, etc.
Metal build-up on the cutting edge of the tool bit is creating a false cutting
edge.
Cutting fluid is required.
Problem: The T ool Holder is Not Feeding
22
The feed pin is broken or out of position.
The feed sprocket shear pin is broken.
The feed screw is stripped.
The feed nut is stripped.
The slide rails are too tight.
92-1333 : Rev. 110404
Page 23
Problem: There's a Loss of Air Power
The air supply pressure is too low.
The air filter is plugged.
The air line size is insufficient.
The air line is too long.
Problem: There's a Loss of Hydraulic Power
The hydraulic supply pressure is too low.
The hydraulic filter is plugged.
The hydraulic line size is insufficient.
The hydraulic line is too long.
Problem: The T ool Bit Will Not Reach the Work
Model 236B Single Point
Incorrect tool blocks are installed for the size of the pipe or tube being
worked on.
Incorrect tool bit is installed.
Problem: The Air Motor Will Not S tart
The air power supply is shut off.
The air motor is damaged and will not run free.
The air motor needs lubrication.
Add lubrication and do not run the air motor for a few minutes, then try running the motor.
Tap on the side of the air motor casing lightly with a piece of wood or with a
soft rubber mallet just in case the vanes may be sticking.
Sand or other foreign material may be in the vanes of the air motor .
Problem: The Hydraulic Motor Will Not Start
The hydraulic power supply is shut off.
The hydraulic motor is damaged and will not run free.
92-1333 : Rev. 110404
23
Page 24
TRI TOOL INC.
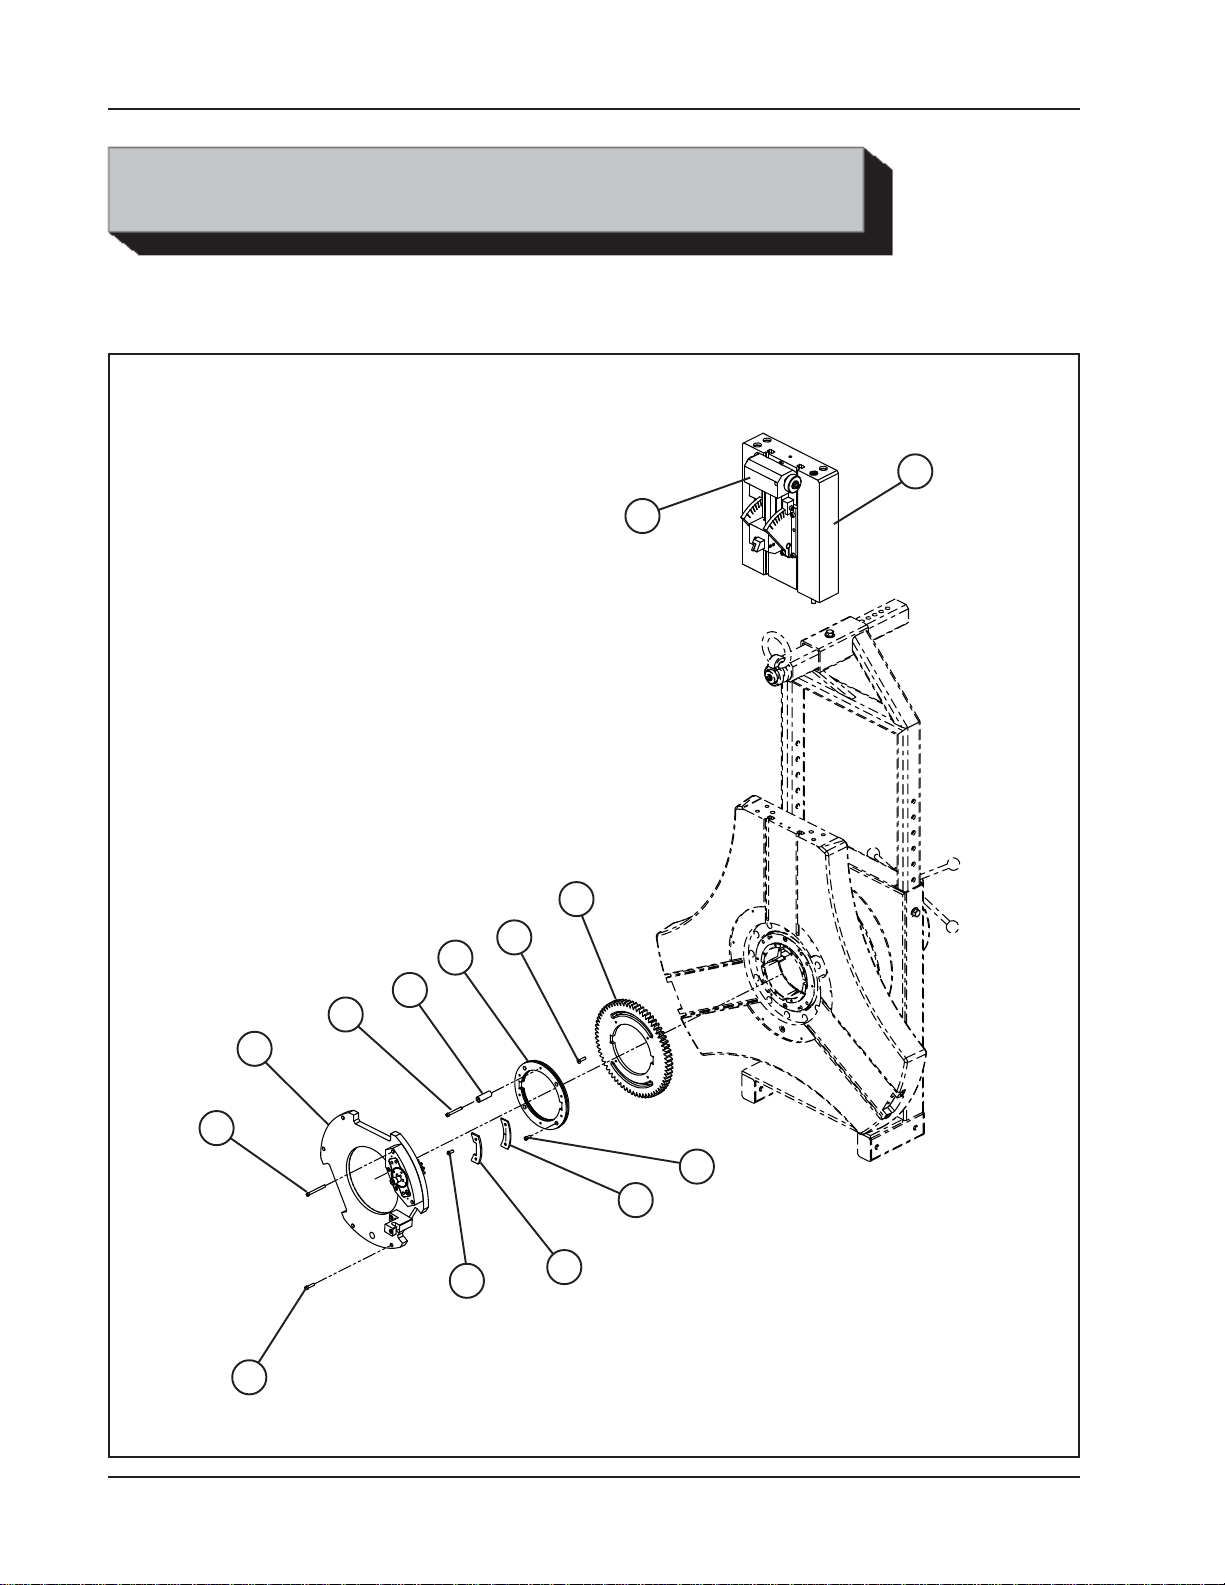
ILLUSTRATED PARTS BREAKDOWN
236B SINGLE POINT (P/N 05-0504)
13
1
10
11
12
6
14
7
5
9
4
3
8
2
24
92-1333 : Rev. 110404
Page 25
Model 236B Single Point
Parts List, 236B Single Point Kit (P/N 05-0504)
Item Part
No. No. Description Qty
1 24-2707 PLATE ASSY, ADAPTER, 236B SP 1
2 28-0432 SEAL, MANDERL 2
3 28-0433 SEAL, MANDERL, KEY WIPER 2
4 33-0038 SCREW,CAP,1/4-20 X 1/2 4
5 33-0042 SCREW,CAP,1/4-20 X 1 4
6 33-0046 SCREW,CAP,1/4-20 X 2 2
7 33-0048 SCREW,CAP,1/4-20 X 2-1/2 2
8 33-0286 SCREW ,BUTTON,1/4-20 X 5/8 4
9 33-0362 SCREW,FLAT ,1/4-20 X 1 4
10 39-1102 GEAR, 236B SP 1
11 43-0818 COVER, GEAR, ASSY 1
12 48-2872 BLOCK, STOP 2
13 82-0141 CUTTER ASSY,224B SINGLE POINT 1
14. 82-0226 HOUSING ASSY, FEED GEAR 1
NOT SHOWN
30-0554 INSERT, TRIANGULAR, .031 R 1
36-0003 WRENCH, L, 3/32 HEX 1
36-0004 WRENCH, L, 7/64 HEX 1
36-0005 WRENCH, L, 1/8 HEX 1
36-0006 WRENCH, L, 9/64 HEX 1
36-0007 WRENCH, L, 5/32 HEX 1
36-0008 WRENCH, L, 3/16 HEX 1
36-0010 WRENCH, L, 1/4 HEX 1
36-0012 WRENCH, L, 3/8 HEX 1
36-0025 WRENCH, T, 3/8 HEX 1
49-0060 HOLDER, TOOL, R.H. 1
92-1333 : Rev. 110404
25
Page 26
TRI TOOL INC.
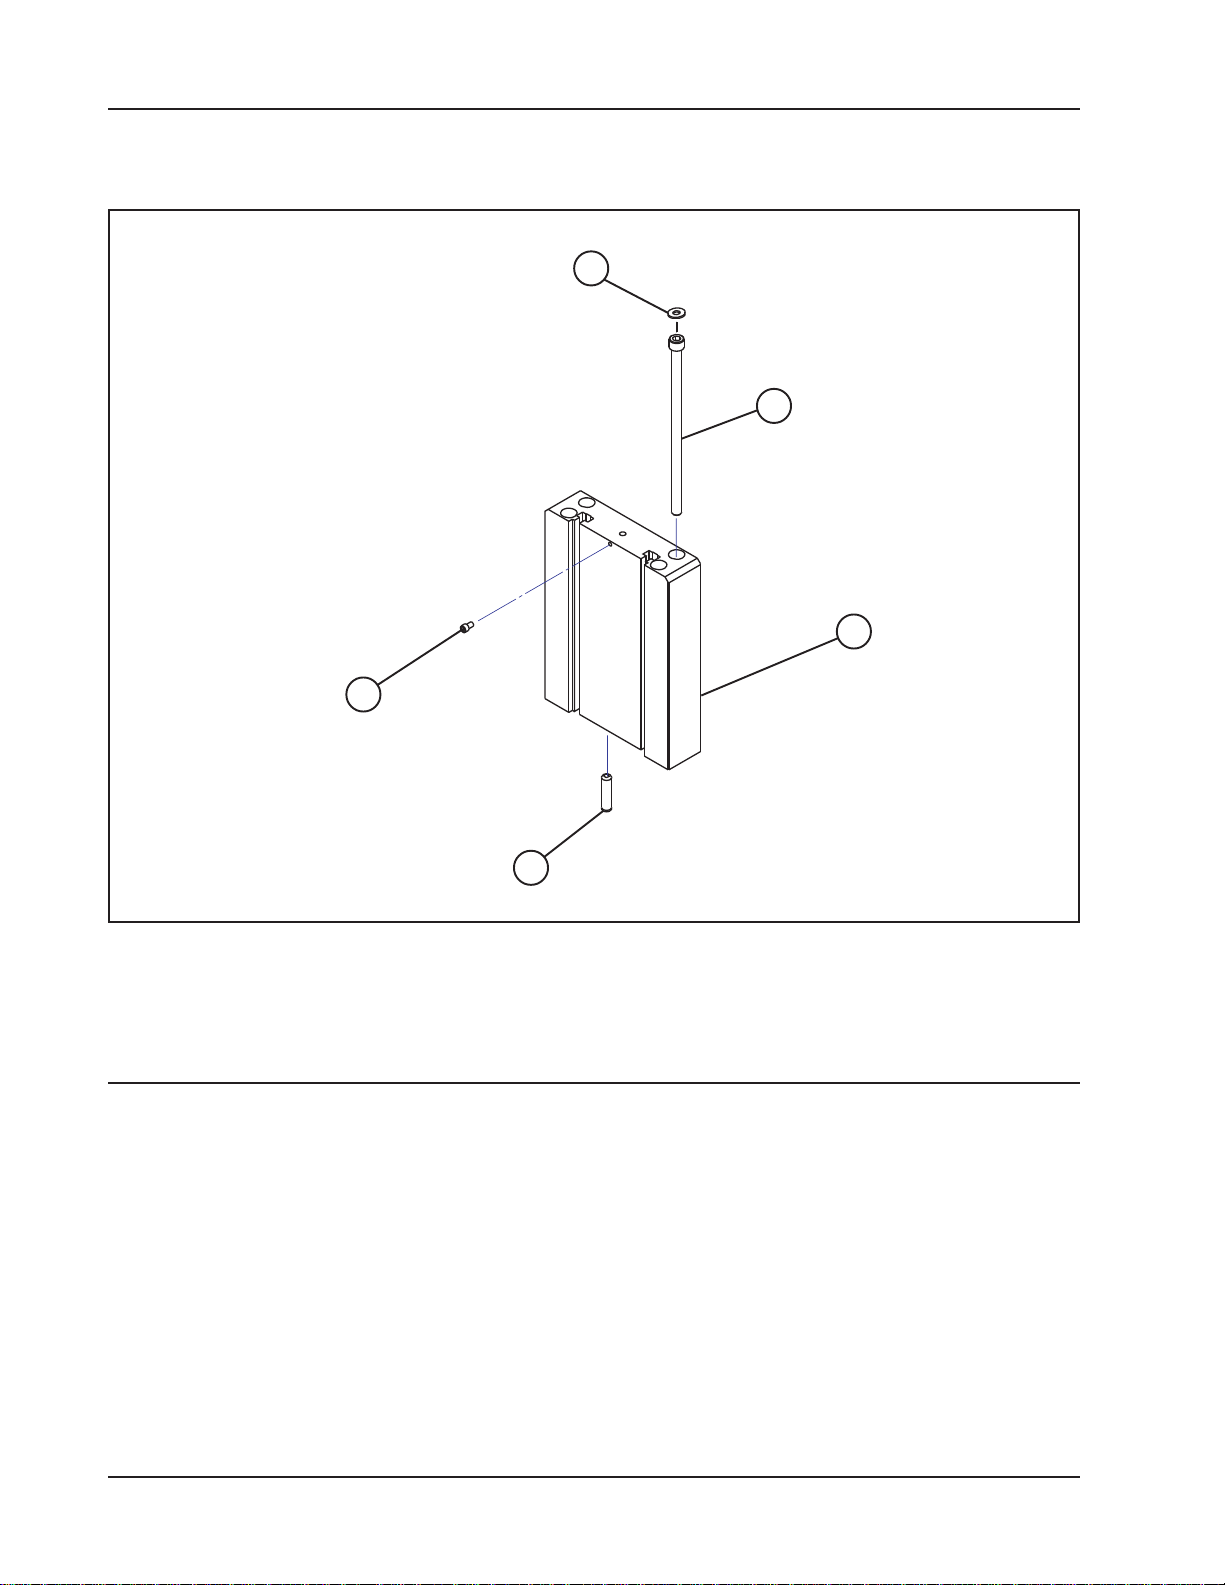
PLATE ASSEMBLY, ADAPTER (P/N 24-2707)
2
5
1
4
3
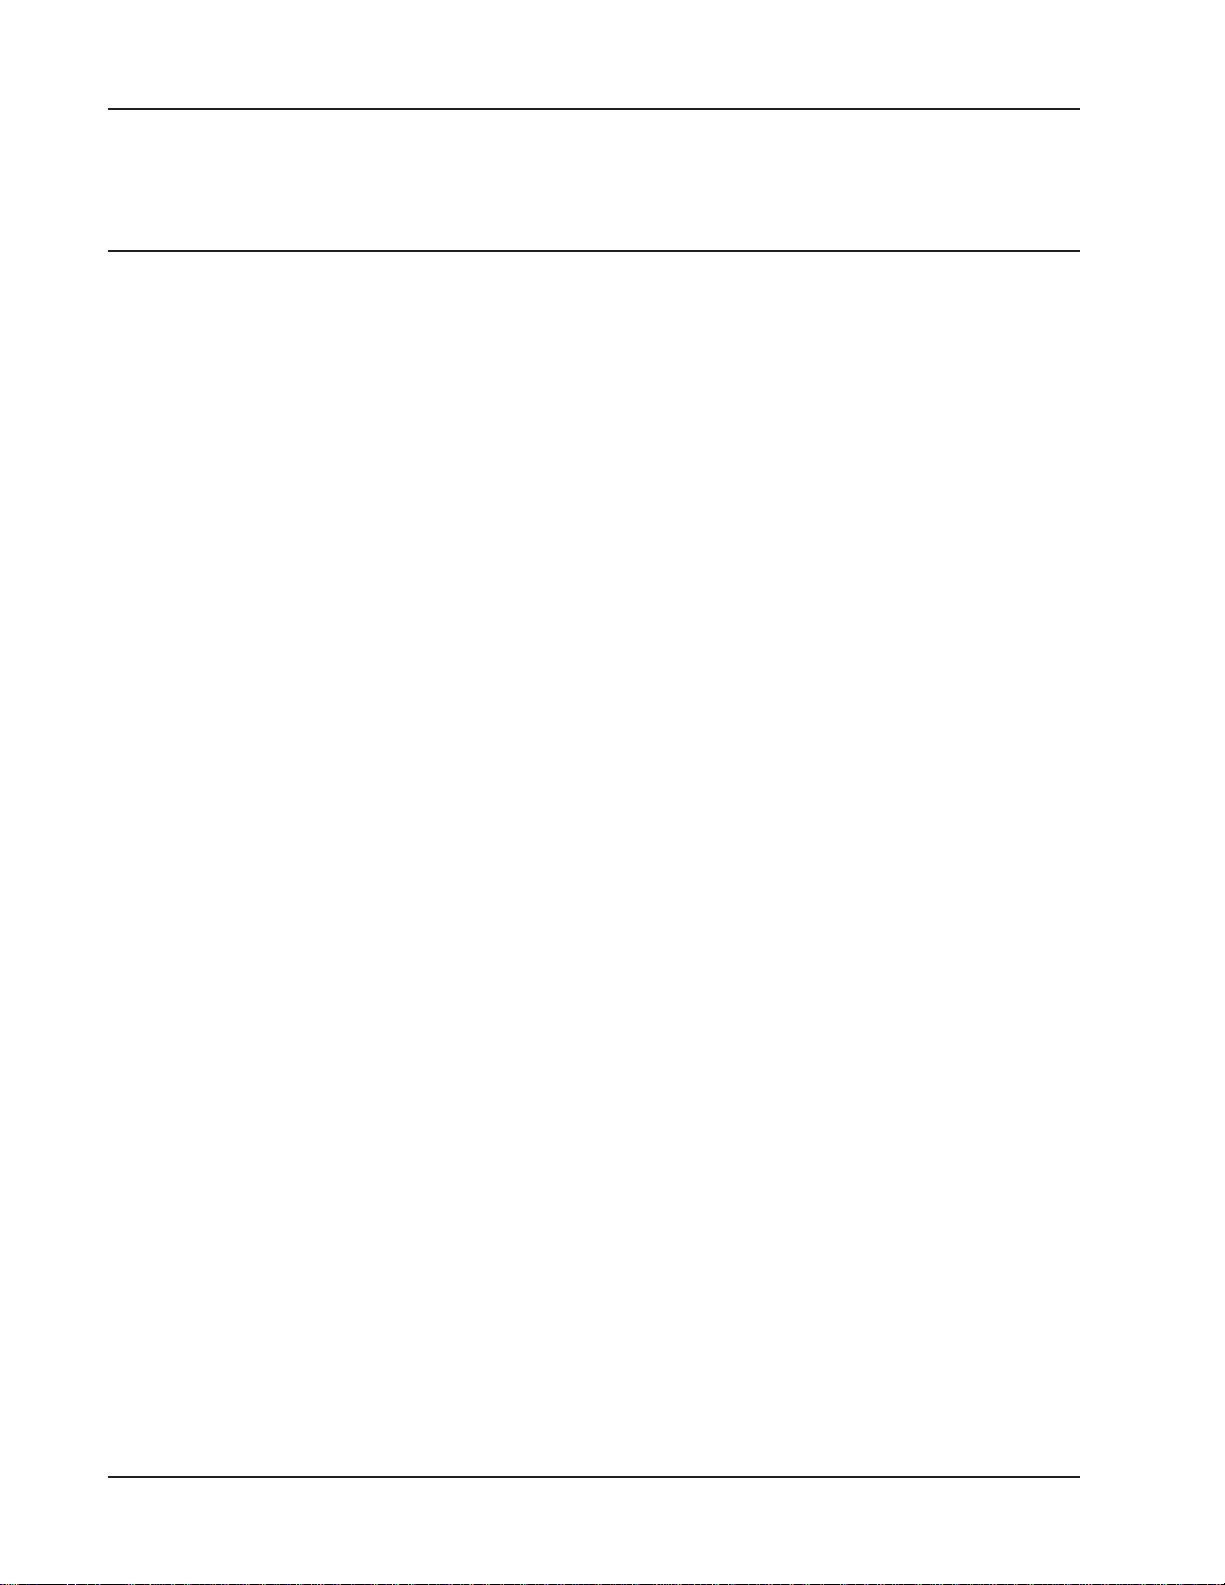
Parts List, Adapter Plate Assembly (P/N 24-2707)
Item Part
No. No. Description Qty
1. 24-2706 PLATE, ADAPTER 1
2. 34-0382 WASHER, NYLON 4
3. 32-0160 PIN, DOWEL, 1/2 DIA X 2” 2
4. 33-0037 SCREW, CAP, 1/4-20 X 3/8” 1
5. 33-2188 SCREW, CAP, 1/2-13 X 11” 4
26
92-1333 : Rev. 110404
Page 27
Model 236B Single Point
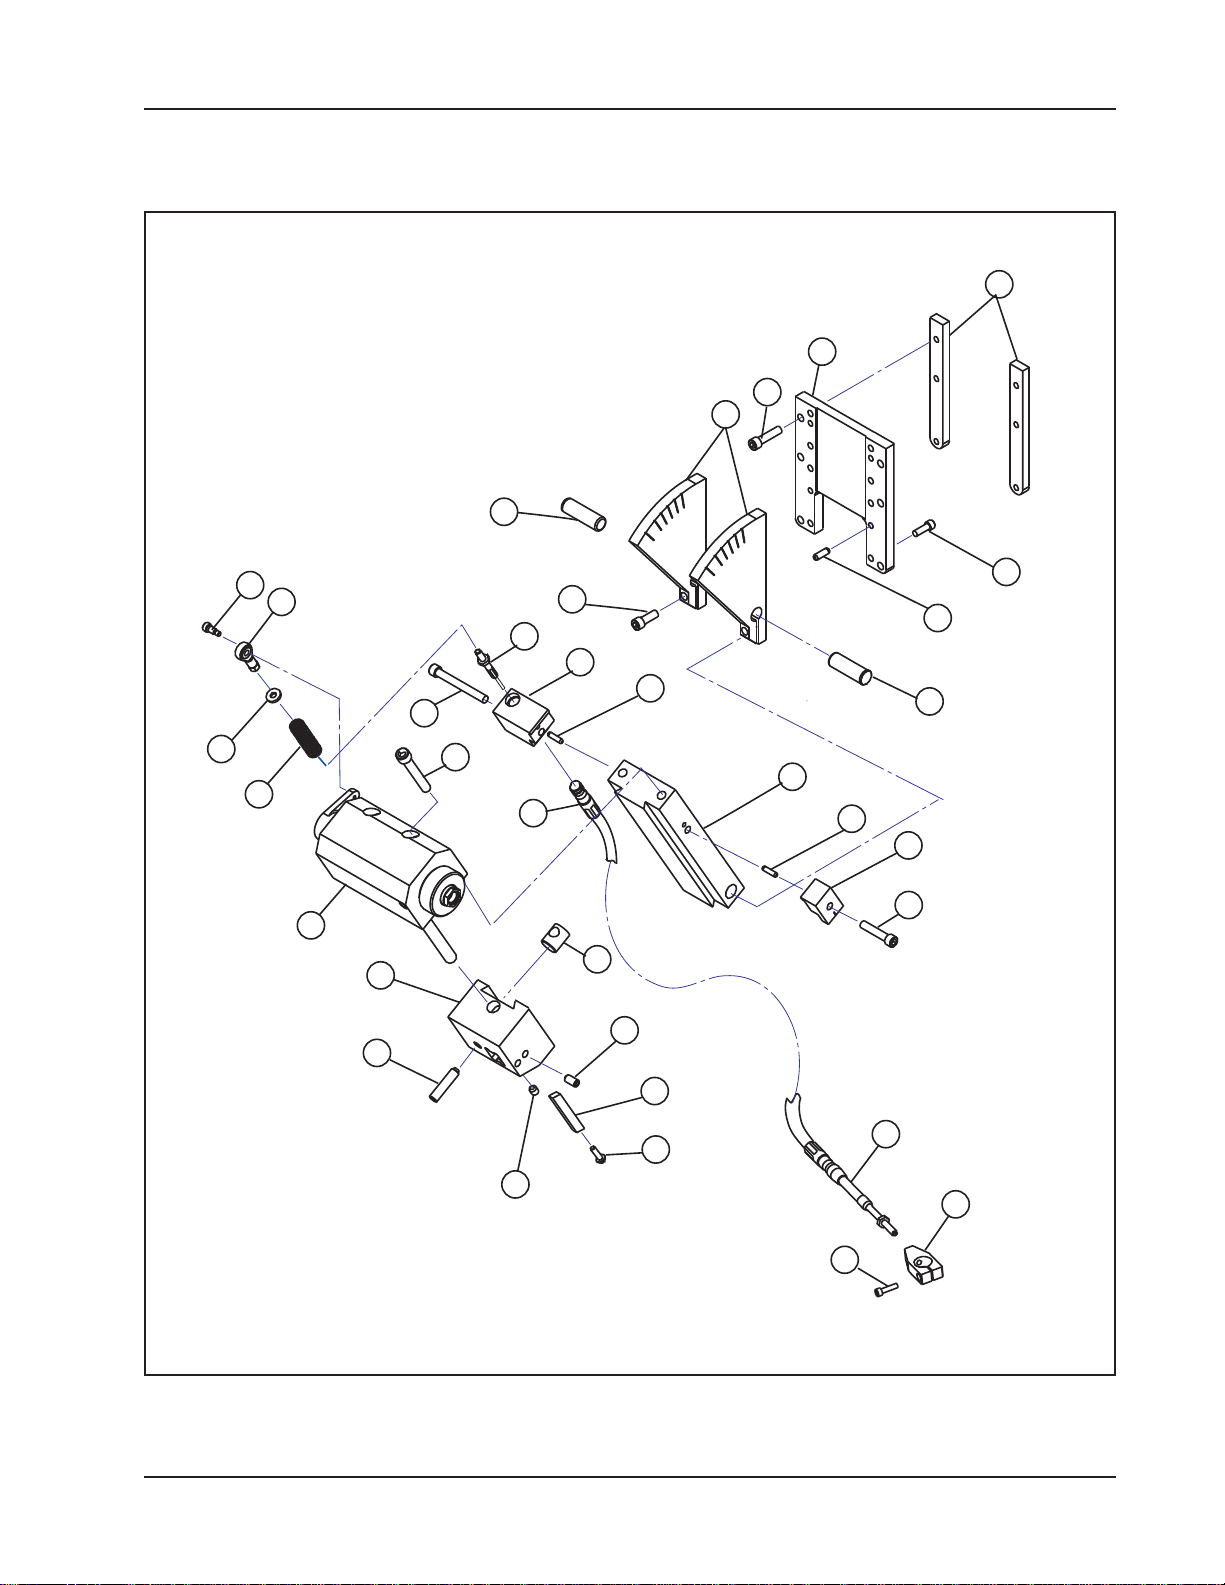
CUTTER ASSEMBLY (P/N 82-0141)
2
16
3
12
4
25
24
27
14
5
18
19
1
28
23
15
9
8
10
29
9
26
21
30
22
10
11
12
6
17
9
92-1333 : Rev. 110404
20
7
13
27
Page 28
TRI TOOL INC.
Parts List, Cutter Assembly (P/N 82-0141)
Item Part
No. No. Description Qty
1. 19-0424 HOUSING , ASSY , GEARBOX 1
2. 24-0733 PLATE,SLIDE,BASE 1
3. 24-0734 PLATE,SIDE 2
4. 26-0828 BAR,RETAIN 2
5. 29-0133 ROD END, 1/4 X 3/4 X 3/8") 1
6. 30-0904 CLAMP,SIDE,RIGHT 1
7. 30-0907 CLAMP,CAM FOLLOWER 1
8. 30-1080 CLAMP,SIDE,LEFT 1
9. 30-2836 CABLE,MOD, 64" LG. 1
10. 32-0081 PIN,DOWEL(3/16 DIA X 3/4") 2
11. 32-0140 PIN,DOWEL(1/4 DIA X 3/4") 4
12. 32-0161 PIN,DOWEL (5/8 DIA X 2") 2
13. 33-0030 SCREW,CAP(# 10-24 X 3/4") 1
14. 33-0040 SCREW,CAP (1/4-20 X 3/4") 8
15. 33-0055 SCREW,CAP (5/16-18 X 7/8") 2
16. 33-0057 SCREW,CAP (5/16-18 X 1 1/4") 6
17. 33-0058 SCREW,CAP (5/16-18 X 1 1/2") 1
18. 33-0063 SCREW,CAP (5/16-18 X 2 3/4") 1
19. 33-0077 SCREW,CAP(3/8-16 X 2 1/2") 2
20. 33-0514 SCREW,SET (5/16-18 X 3/8") 1
21. 33-0517 SCREW,SET (5/16-18 X 5/8") 3
22. 33-0955 SCREW,GIB 1
23. 33-1314 SCREW,SET, HALF DOG (3/8-16 X 1 1/2") 1
24. 33-1535 SCREW, SHLDR (1/4 X 3/8") 1
25. 34-0026 WASHER,FLAT 1
26. 35-0270 NUT,FEED,1/2 -20 1
27. 40-0045 SPRING ,COMP ( 5/8 DIA X 4") 1
28. 49-0091 HOLDER,TOOL 1
29. 66-0078 BASE,SLIDE 1
30. 66-0079 GIB,TAPERED 1
28
92-1333 : Rev. 110404
Page 29
Model 236B Single Point
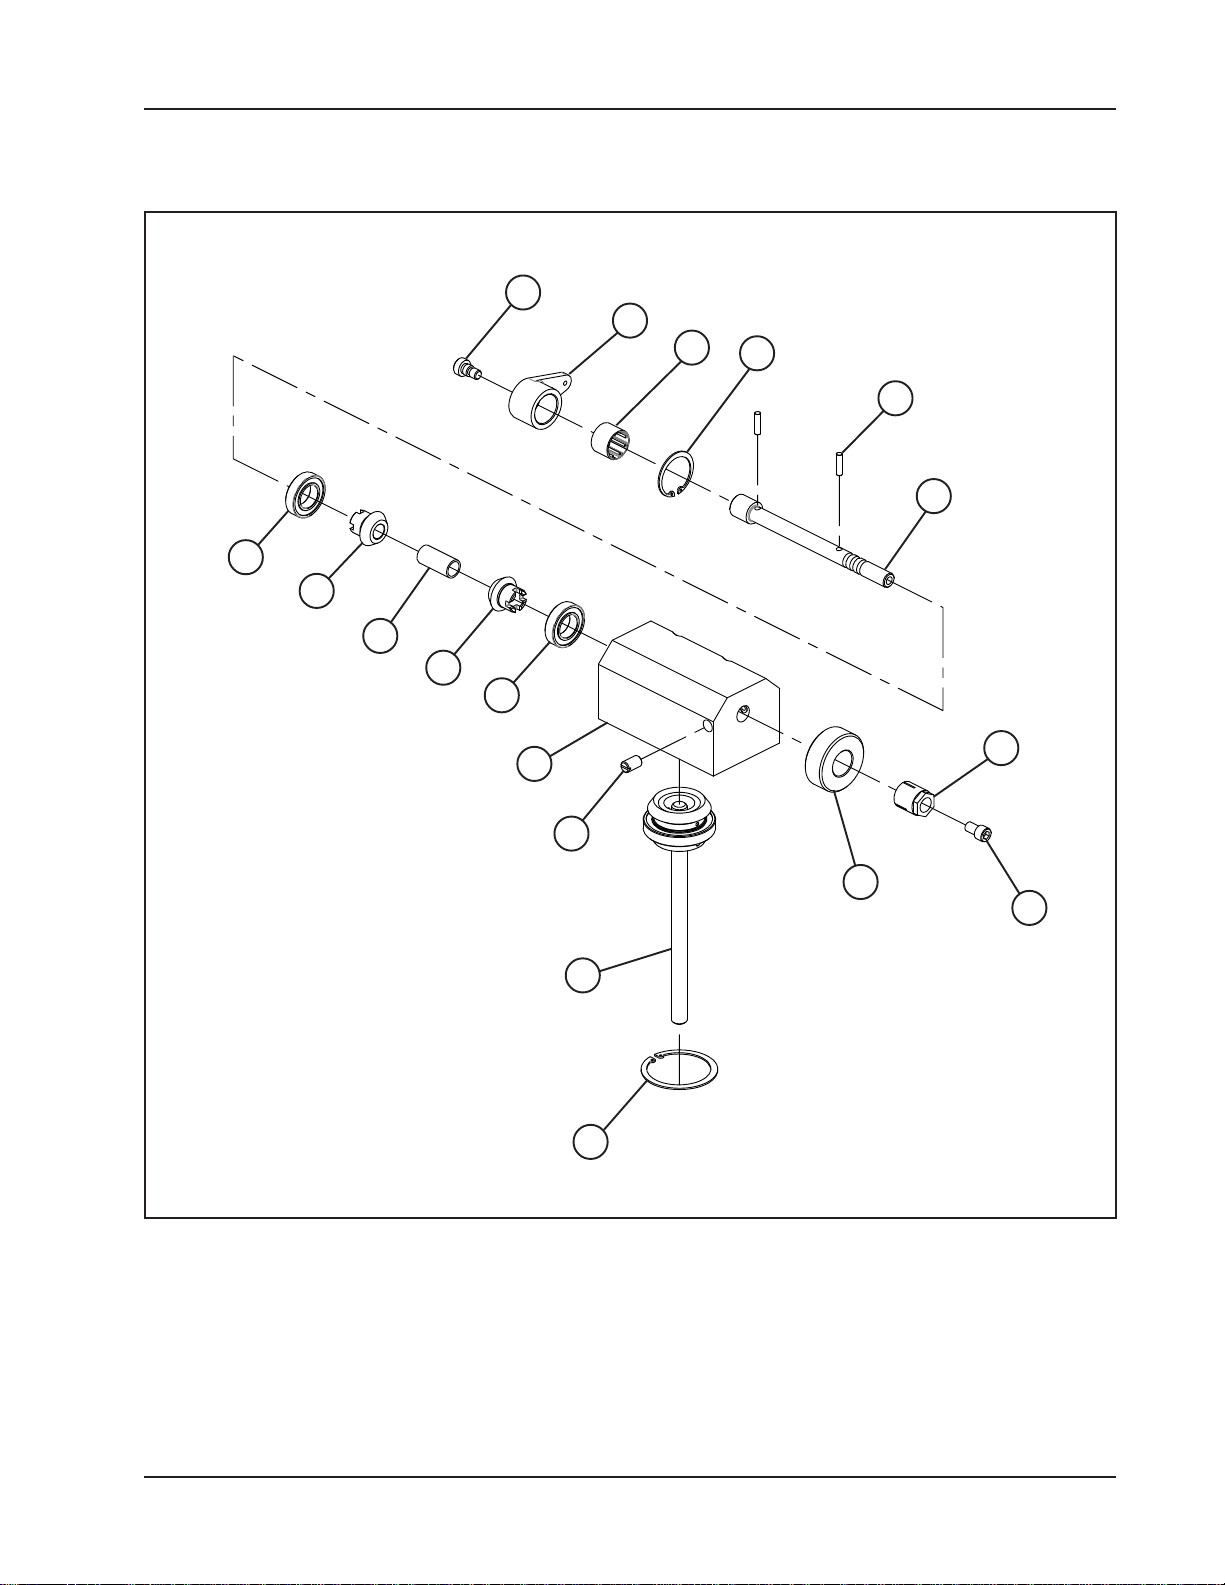
HOUSING ASSEMBLY, GEARBOX (P/N 19-0424)
12
16
8
3
13
15
13
3
6
9
2
1
7
14
11
4
5
10
92-1333 : Rev. 110404
29
Page 30
TRI TOOL INC.
Parts List, Gearbox Housing Assembly (P/N 19-0424)
Item Part
No. No. Description Qty
1. 19-0418 HOUSING , GEAR 1
2. 20-0364 SHAFT, MAIN 1
3. 29-0029 BRG, BALL, .79 X 1.46 X .35 2
4. 30-0489 RING , RETAIN, INT , 2-5/16 ID 1
5. 30-0507 MOUNT, KEYLESS SHAFT 1
6. 30-0910 RING , RET AIN, INT., 37 MM 1
7. 30-0911 PLUNGER, BALL, 3/8-16 X 5/8 2
8. 30-0912 CLUTCH, ROLLER 1
9. 32-0305 PIN, MOD, DOWEL, 3/16 X 3/4 2
10. 33-0052 SCREW, CAP, 5/16-18 X 1/2 1
11. 33-1533 SCREW ASSEMBLY, FEED 1
12. 33-1536 SCREW , MOD, SHOULDER, 3/8 X 1/4 1
13. 39-0482 GEAR, MOD, BEVEL, 20 DEG P.A. 14DP 2
14. 42-0104 KNOB, FEED 1
15. 44-0275 SPACER, GEAR 1
16. 63-0096 ARM, ACTUATOR 1
30
92-1333 : Rev. 110404
Page 31
Model 236B Single Point
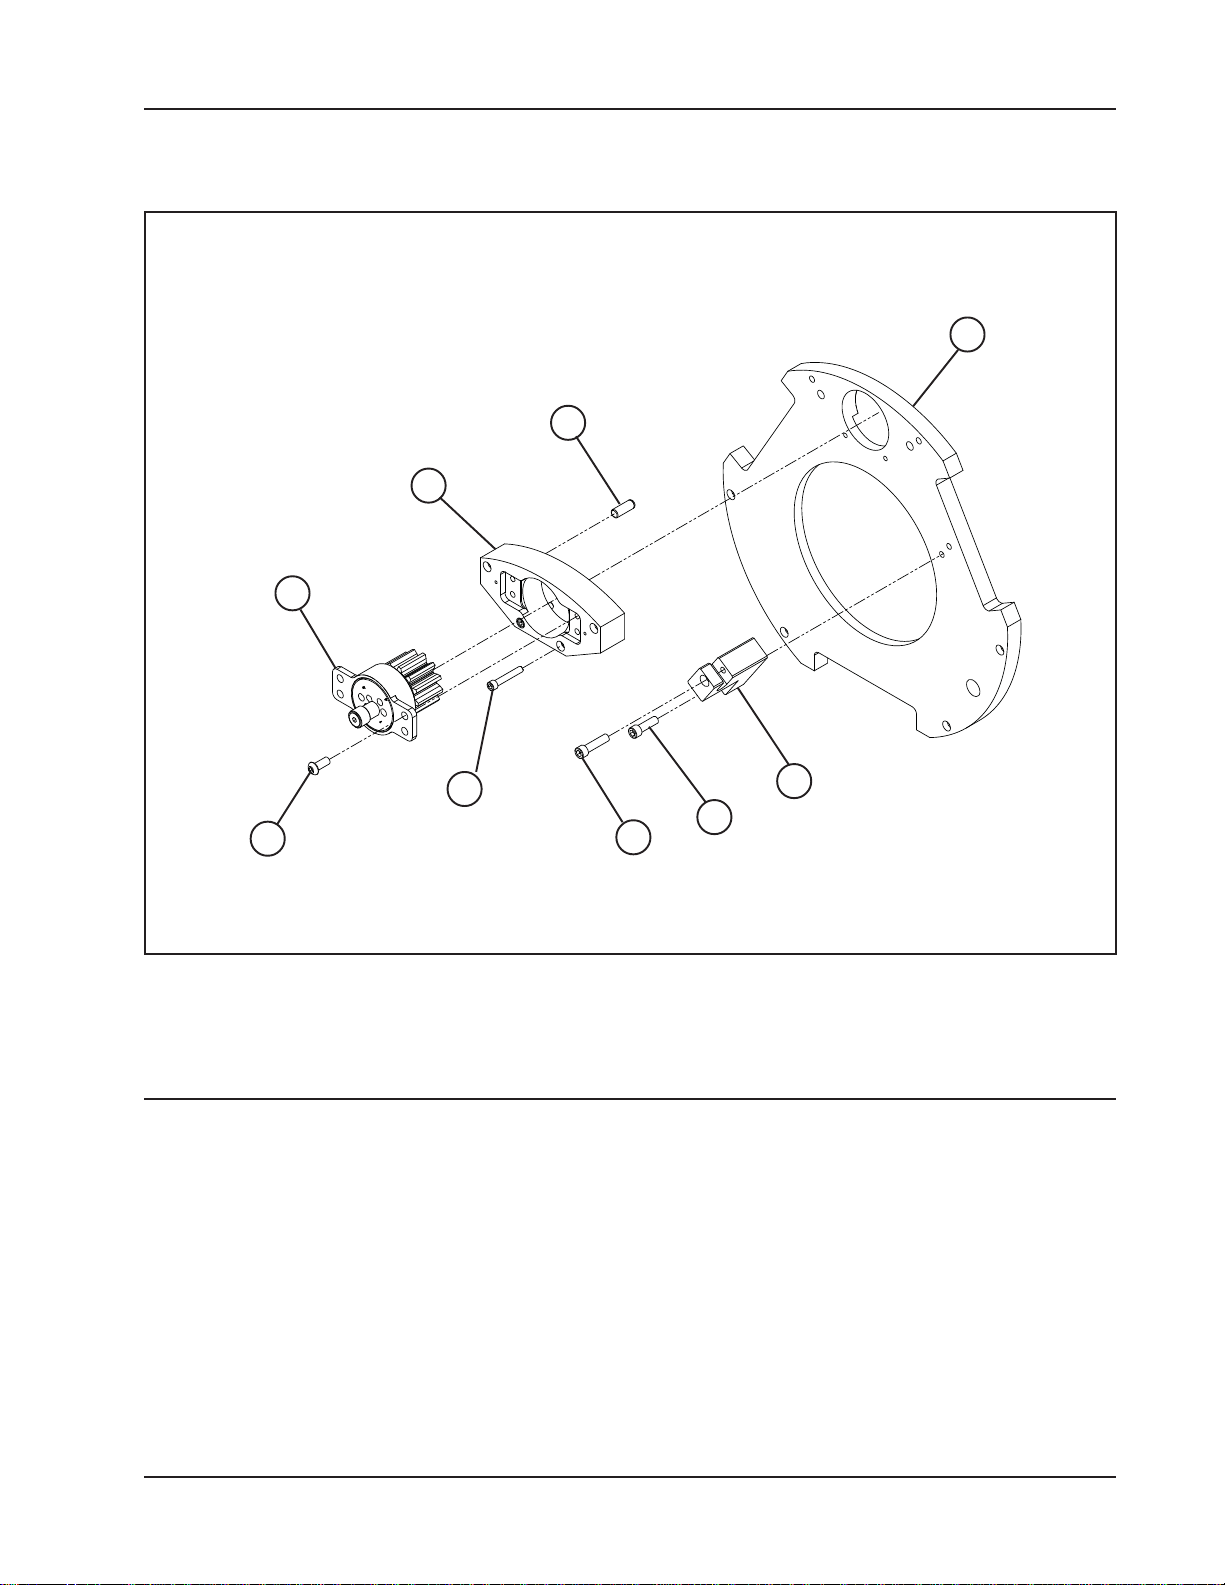
FEED GEAR HOUSING ASSEMBLY (P/N 82-0226)
3
5
2
1
6
7
9
8
4
Parts List, Feed Gear Housing Assembly (P/N 82-0226)
Item Part
No. No. Description Qty
1. 19-1258 HOUSING, ASSY INDEX PLA TE 1
2. 19-1353 HOUSING, FEED GEAR, SP 1
3. 24-3295 PLATE, FEED GEAR 1
4. 30-4508 CLAMP, CABLE, DOGLEG 1
5. 32-0105 PIN,DOWEL,3/8 DIA X 1 2
6. 33-0044 SCREW,CAP,1/4-20 X 1-1/2 2
7. 33-0056 SCREW,CAP,5/16-18 X 1 2
8. 33-0057 SCREW,CAP,5/16-18 X 1-1/4 1
9. 33-0293 SCREW ,BUTTON,5/16-18 X 3/4 4
92-1333 : Rev. 110404
31
Page 32
TRI TOOL INC.
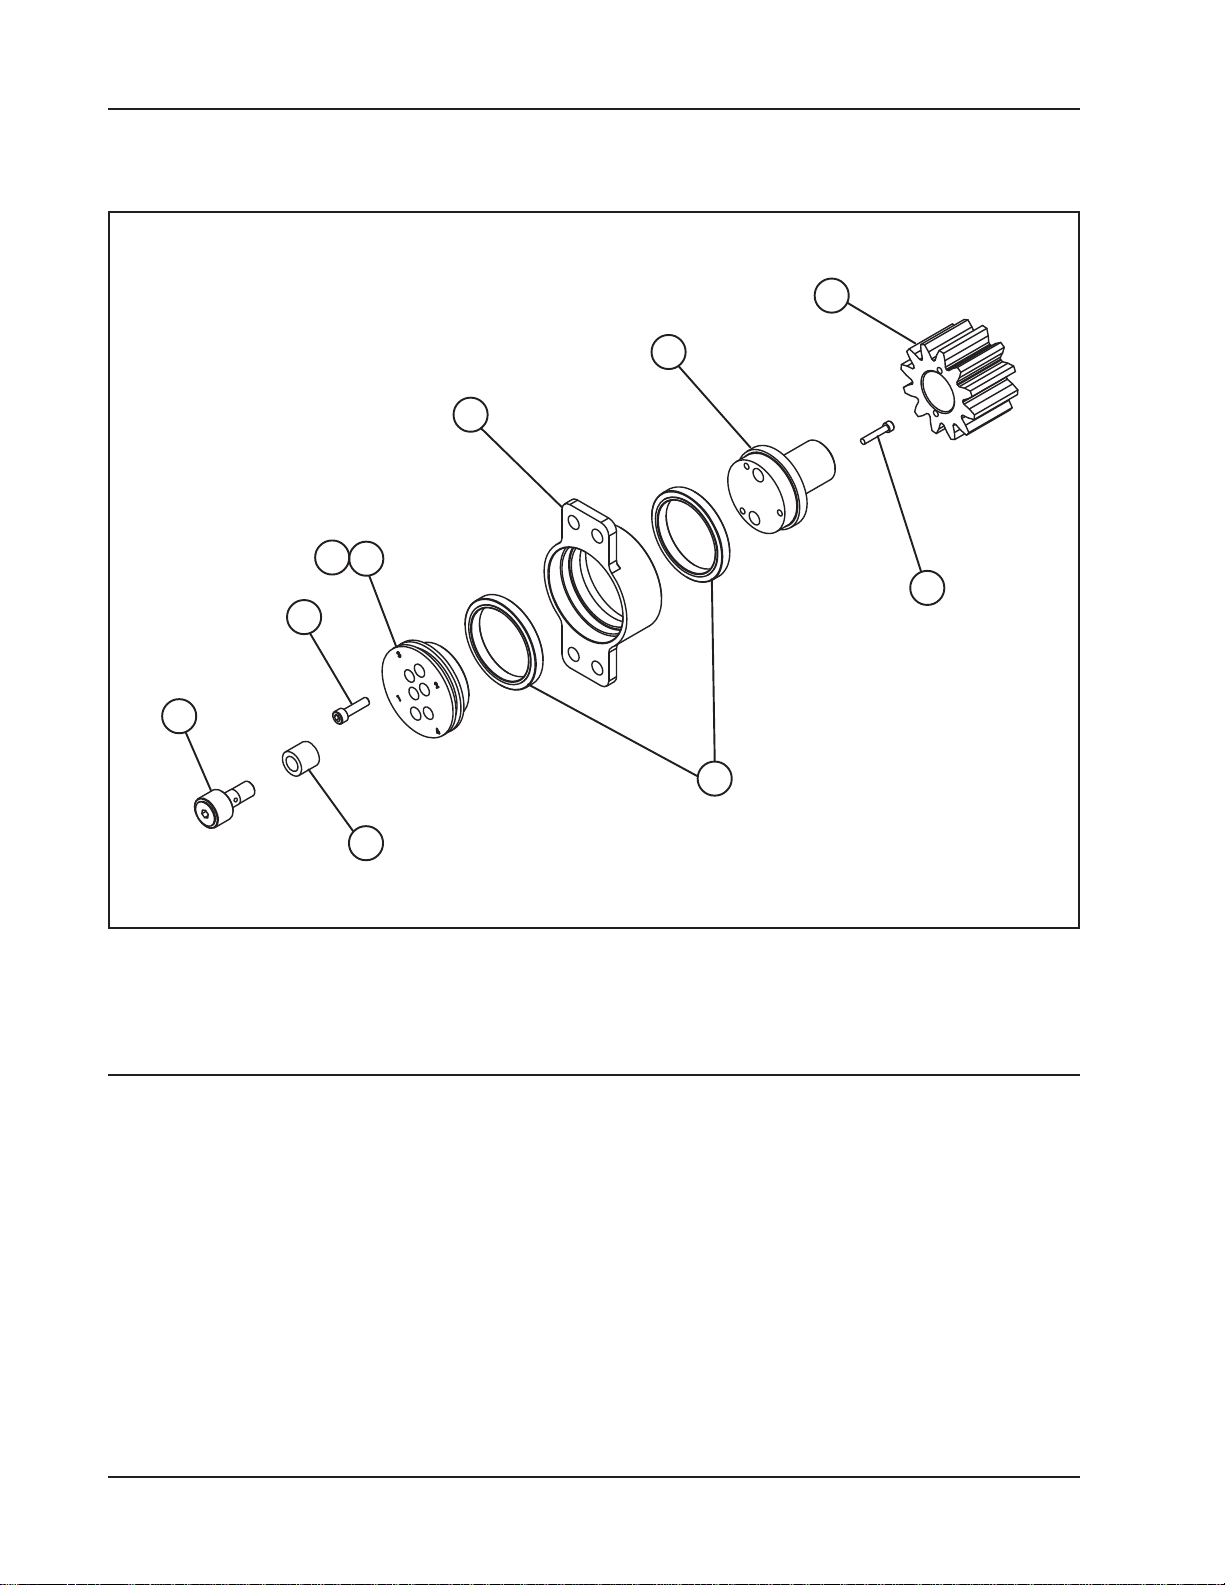
HOUSING ASSEMBLY, INDEX PLATE (P/N 19-1258)
9
2
1
3
4
7
8
6
5
10
Parts List, Index plate Housing Assembly (P/N 19-1258)
Item Part
No. No. Description Qty
1. 19-0428 HOUSING ,INDEX PLATE 1
2. 24-1576 HUB,GEAR 1
3. 24-1577 PLATE,INDEX,236B 1
4. 28-0057 SEAL, FELT, 1/8 X 3/16 X BULK 7
5. 29-0104 BRG,BALL,1-13/16 X 2-1/4 X9/32 2
6. 29-0219 CAM FLLWR 3/4 O.D. X 1/2 1
7. 33-0015 SCREW,CAP,#6-32 X 3/4 3
8. 33-0030 SCREW,CAP,10-24 X 3/4 2
9. 39-0852 GEAR,MOD,SPUR,6DP,12T ,2.0 DP 1
10. 44-0276 SPACER 1
32
92-1333 : Rev. 110404
 Loading...