

Page 1
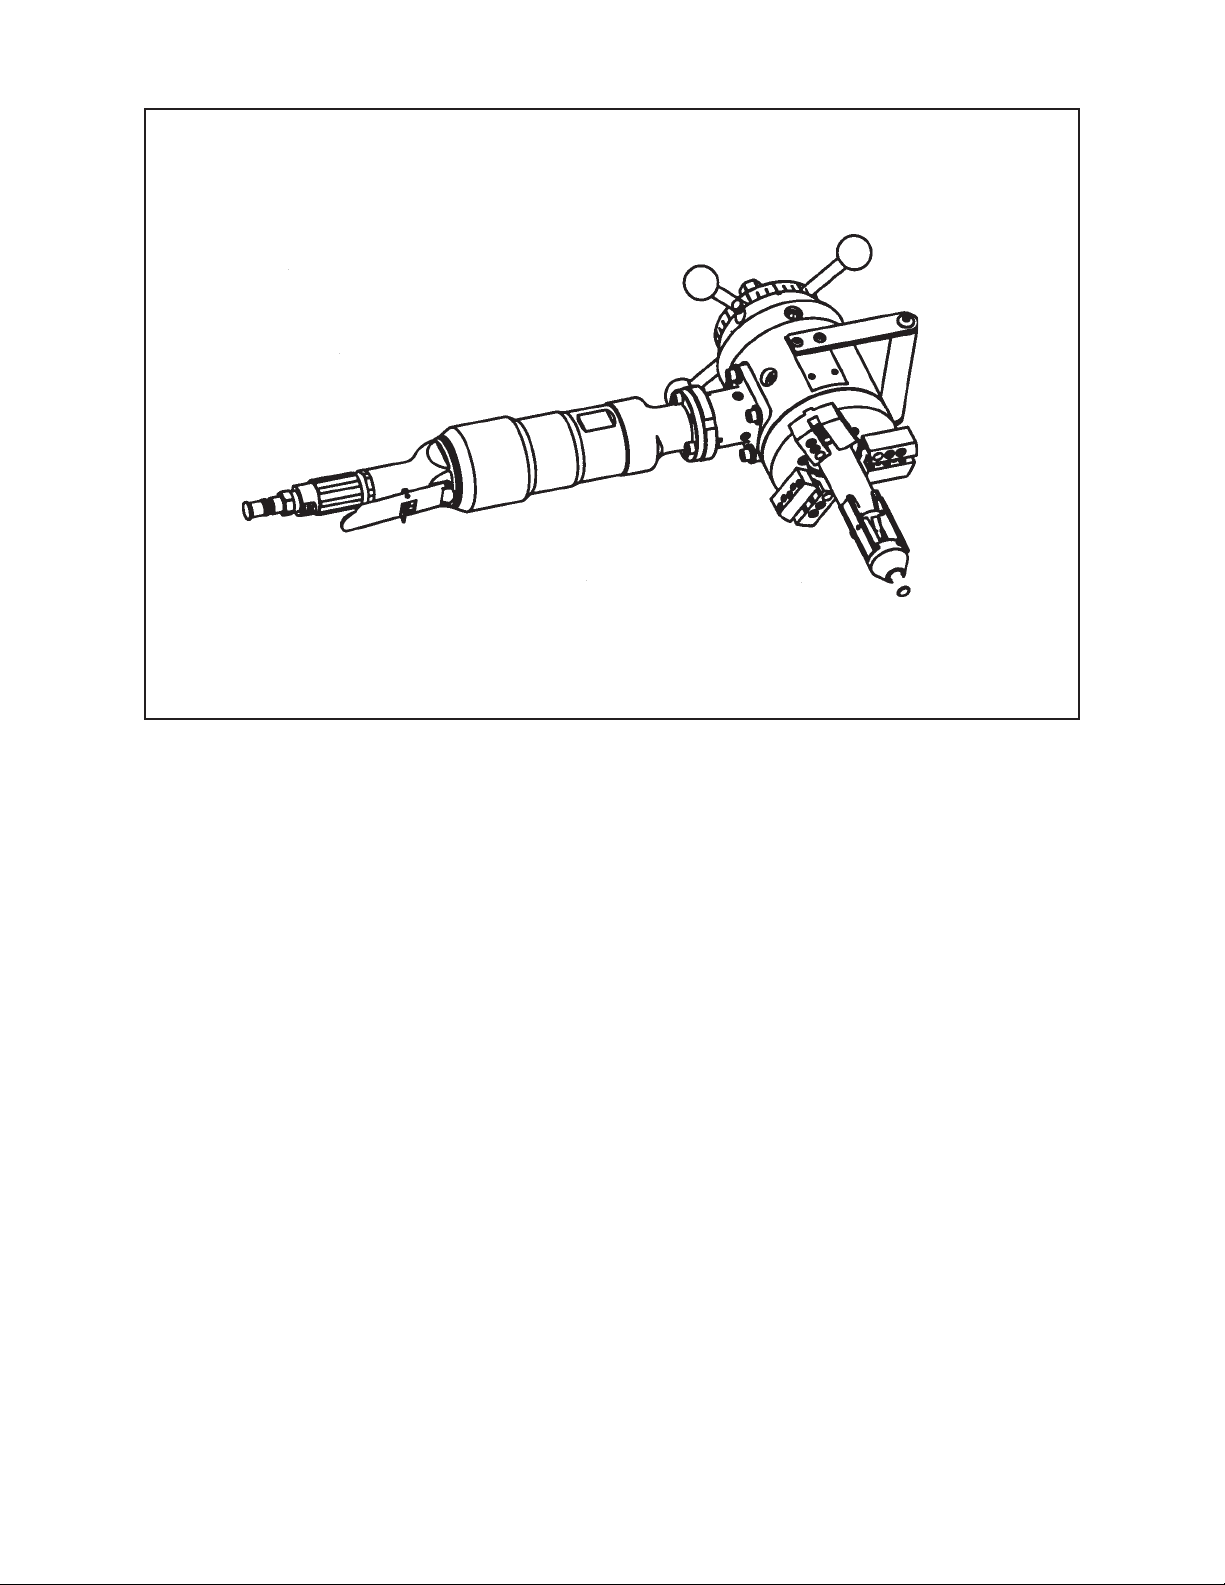
TABLE OF CONTENTS
CUSTOMER MESSAGE Inside Front Cover
SAFETY PRECAUTIONS 3
92-0211 Rev. 050224
Model 206B BEVELMASTER™
GENERAL DESCRIPTION 6
SPECIFICATIONS 7
MAINTENANCE 14
OPERATION 17
CUTTING SPEEDS AND FEEDS 23
JAW BLOCKS and RAMPS 25
TOOL BITS 26
TROUBLE SHOOTING 32
ACCESSORIES 34
ILLUSTRATED PARTS BREAKDOWN 35
TOOL BIT RESHARPENING POLICY Inside Back Cover
WARRANTY INFORMATION Inside Back Cover
Page 2
Copyright 2005
Proprietary property of TRI TOOL Inc.
No reproduction, use, or duplication of the information
shown hereon is permitted without the express written
consent of TRI TOOL Inc.
Page 3
SAFETY PRECAUTIONS
IN GENERAL
When using rotating head cutting equipment, basic safety precautions should always
be followed to reduce the risk of personal injury.
Operate this tool only in accordance with specific operating instructions.
Do not override the deadman switch on the power unit. Locking down, ob-
WARNING:
DRESS CONSIDERATIONS
structing, or in any way defeating the deadman switch on the power drive unit
may result in serious injury.
Model 206B BEVELMASTER™
Use standard safety equipment. Hard hats, safety shoes, safety harnesses, protective clothes, and other safety devices should always be used when appropriate.
Use safety glasses. Do not operate cutting tools without eye protection.
Dress properly. Do not wear loose clothing or jewelry. They can be caught in rotating and moving parts. Avoid slippery floors or wear nonskid footwear. If you have
long hair, wear protective hair covering to contain it.
WORK AREA
Keep the work area clean. Cluttered work areas and benches invite injuries.
Consider the work area environment. Keep the area well lit. Keep electrical cords,
cables, rags, rigging straps, and etc. clear of rotating equipment. Do not use powercutting tools in the presence of flammable liquids and gasses.
Keep visitors away. Do not let visitors or untrained personnel at or near operating
tools. Enforce eye protection requirements for all observers.
Do not over reach. Keep proper footing at all times.
Stay alert. Watch what you are doing. Use common sense. Do not operate tools
when you are tired.
92-0211 : Rev. 050224
3
Page 4
TRI TOOL INC.
TOOL CARE
Maintain tools with care. Keep tools in good operating condition. Sharp tool bits
perform better and safer than dull tool bits. Well maintained tools function properly
when needed.
Check for damaged parts. If a tool has malfunctioned, been dropped or hit, it must
be checked for damage. Run no-load tests and feed function checks. Do a complete visual inspection.
Electric motors. Use only with proper AC voltage power sources and observe all
normal electric shock hazard procedures.
Do not abuse power and control cords. Pulling or running over cords and cables
can result in electrical shock hazards and malfunctions. Keep control and power
cords out of all cutting fluids and water.
Hydraulic drives. Observe proper procedures for electrically driven power sources.
Avoid damage to hydraulic lines. Keep quick-disconnects clean. Grit contamination
causes malfunctions.
Air tools. Check the exhaust muffler. Broken or damaged mufflers can restrict air
flow or cause excessive noise. Use air motors only with a filtered, lubricated and
regulated air supply. Dirty air, low-pressure air or over pressure air will cause malfunctions, including delayed starting.
AREA EQUIPMENT
Secure work. Whenever possible use clamps, vises, chains and straps to secure
pipe.
Make sure the tool is secured; it is safer to have both hands free to operate the tool.
TOOL USE
Use the right tool and tool bit for the job. Do not use a tool, which is incorrect for the
job you are doing.
Keep the tool bits fully engaged in the tool bit holders. Loose bits are a safety hazard.
4
92-0211 : Rev. 050224
Page 5
Model 206B BEVELMASTER™
Disconnect power supply during setup and maintenance. Use all 'Stop' or 'Shut off'
features available when changing or adjusting tool bits, maintaining the tool, or when
the tool is not in use.
Remove adjusting keys and wrenches before applying power to the equipment.
Develop a habit of checking the tool before turning it on to make sure that all keys
and wrenches have been removed.
Do not force tools. Tools and tool bits function better and safer when used at the
feed and speed rate for which they were designed.
Do not reach into rotating equipment. Do not reach into the rotating head stock to
clear chips, to make adjustments, or to check surface finish. A machine designed to
cut steel will not stop for a hand or an arm.
Handle chips with care. Chips have very sharp edges and are hot. Do not try to pull
chips apart with your hands; they are very tough.
Avoid unintentional starts. Do not carry or handle tools with your hand on the operating switches or levers. Do not lay the tool down in a manner that will start the
drive. Do not allow the tool to flip around or move when adjusting or changing tool
bits.
Store idle tools properly. Disconnect tools from the power source and store in a safe
place. Remove tool bits for safe handling of the tool.
92-0211 : Rev. 050224
5
Page 6
TRI TOOL INC.
GENERAL DESCRIPTION
The Model 206B is a Pipe Beveler designed for facing, beveling and/or
counterboring the ends of pipe and/or tubing in preparation for welding.
These machining operations may be performed either simultaneously or separately.
Pipe weld end preparations that meet all existing conventional codes including the
more stringent nuclear codes may be machined using the Model 206B.
The various interchangeable jaw blocks and ramps will secure the Model 206B Pipe
Beveler to pipe and tubing having an inside diameter ranging from 1.63” (41.4 mm)
through 6.49” (164.8 mm).
The expanding mandrel provides fast, accurate self-centering and alignment to the
pipe or tubing to be machined.
The Model 206B accepts the reaction torque generated by the machining operations
through the mandrel.
No additional restraining devices are required.
6
92-0211 : Rev. 050224
Page 7
SPECIFICATIONS
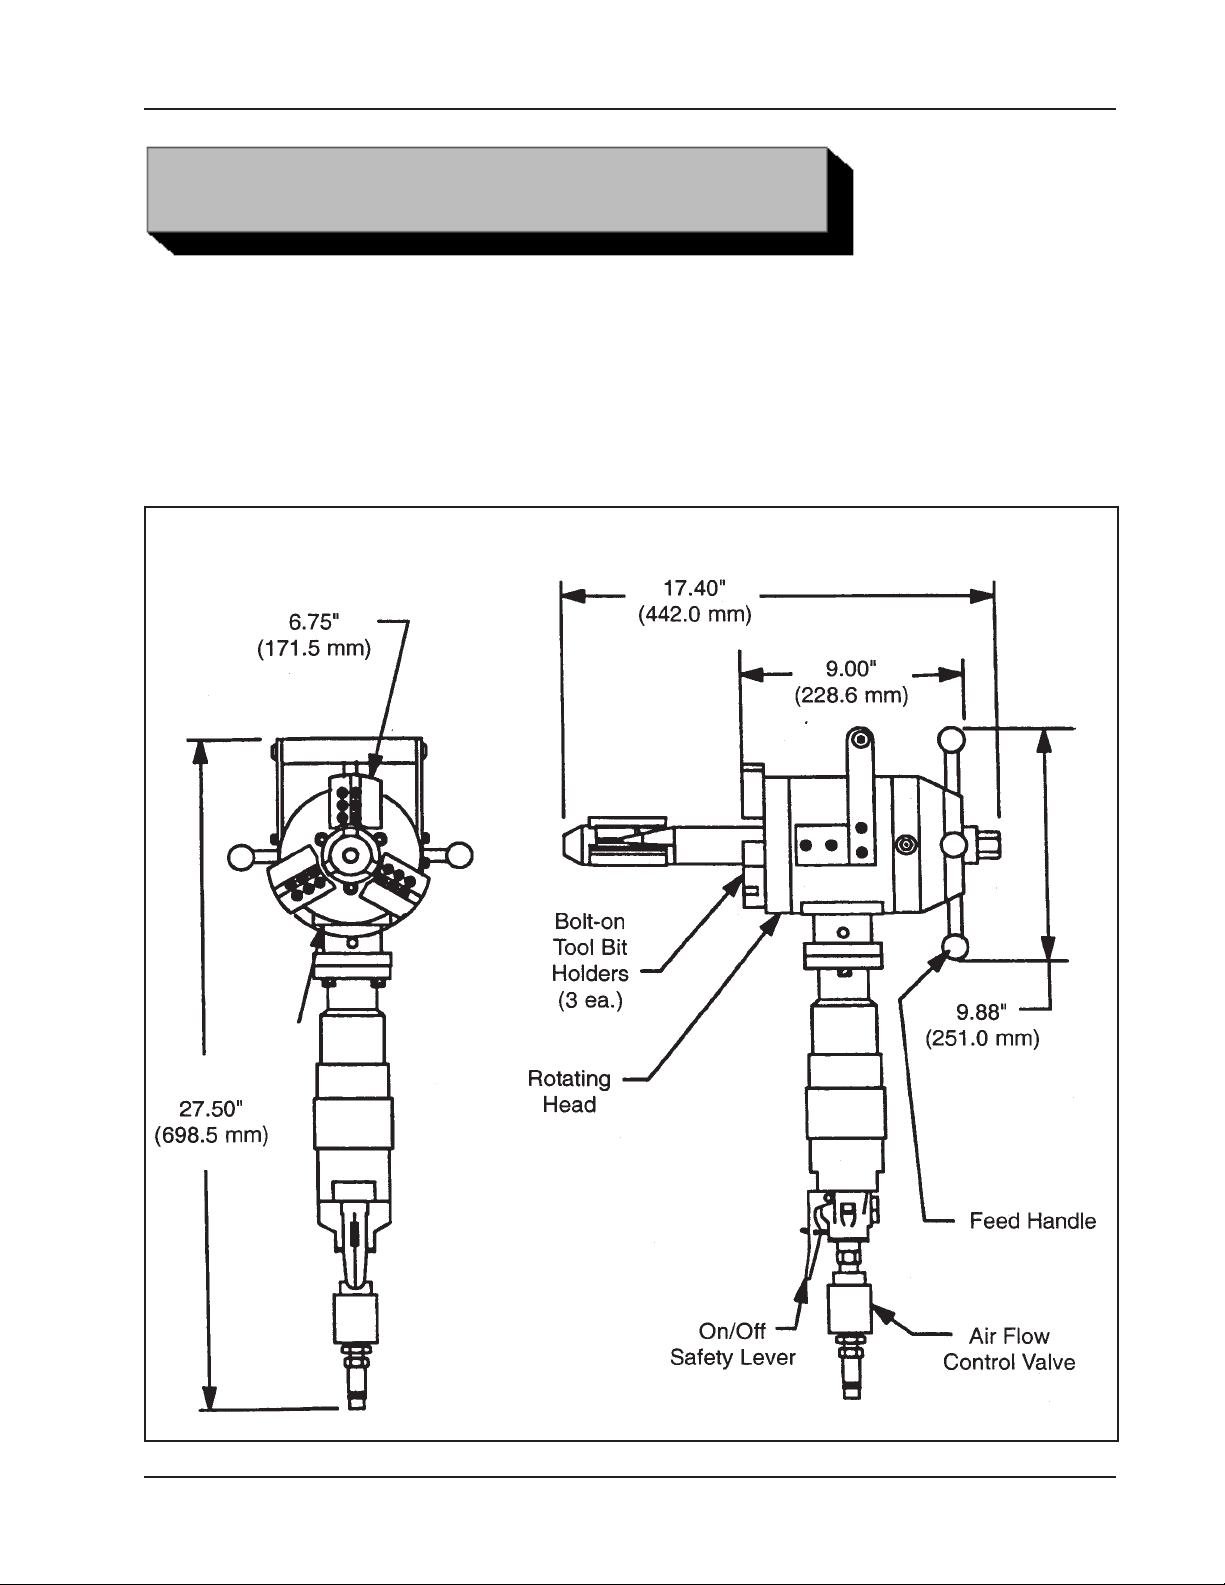
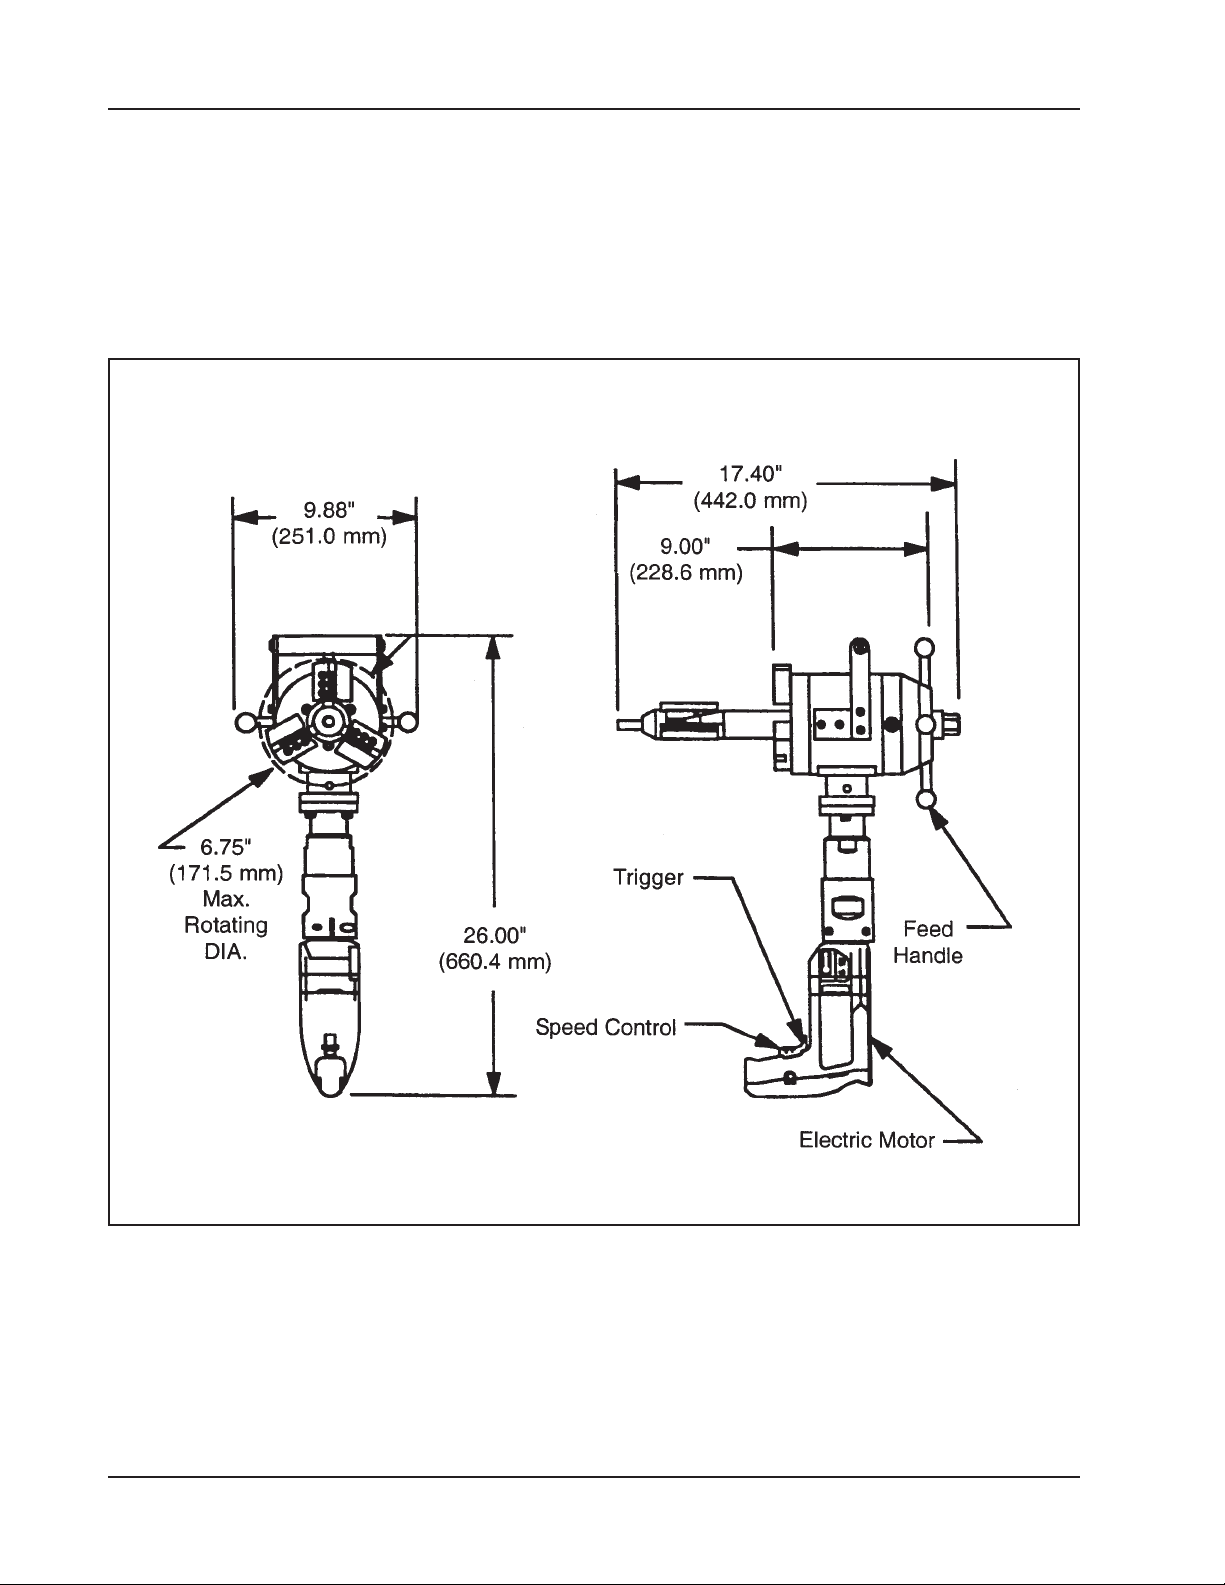
MODEL 206B WITH AIR MOTOR
Weight (Less the Mandrel) 34 lbs (16 kg)
Power Requirements 85 cfm @ 90 psi (35 L/s @ 621 kPa)
Model 206B with an Air Motor Envelope Drawing
Model 206B BEVELMASTER™
92-0211 : Rev. 050224
7
Page 8
TRI TOOL INC.
PIPE CUTTING CAP ACITIES
Basic Pipe Sizes
1 1/2” Pipe Schedules 5 and 10
2" and 2 1/2" Pipe Schedules 5 through 160
3" through 6" Pipe All Schedules
Basic Tube Sizes
Up to .875” (22.2 mm) wall tubing with a maximum OD of 6.63” (168.4 mm)
and a minimum ID of 1.63” (41.4 mm) may be beveled with standard procedures.
Wall Thickness Capacity
Wall thickness of all standard pipe schedules, .864” (21.9 mm) maximum, in
the range listed.
Tubing with greater wall thickness may be handled provided the ID is greater
than 1.63” (41.4 mm) and the OD is less than 6.63" (168.4 mm).
Contact TRI TOOL INC. for heavier wall procedures.
Counterboring Operation
The machine will counterbore pipe and tubing with an ID range of 2.00” (50.8
mm) to 6.41” (162.8 mm).
Material Cutting Capability
Mild steels, chrome steels (Rc 35 max.), stainless steel, copper-nickel and
aluminum without limitations except size and wall thickness as specified
under ‘Wall Thickness Capacity’.
Inconnel and some other high temperature alloys may require special procedures as a function of wall thickness and type of end preparation.
Contact the TRI TOOL INC. Engineering department for details.
8
92-0211 : Rev. 050224
Page 9
Headstock Speeds
Maximum Headstock Speed 78 rpm
Headstock Speed at maximum H.P. 39 rpm
Functional Speed Range 10 to 60 rpm
Model 206B BEVELMASTER™
92-0211 : Rev. 050224
9
Page 10
TRI TOOL INC.
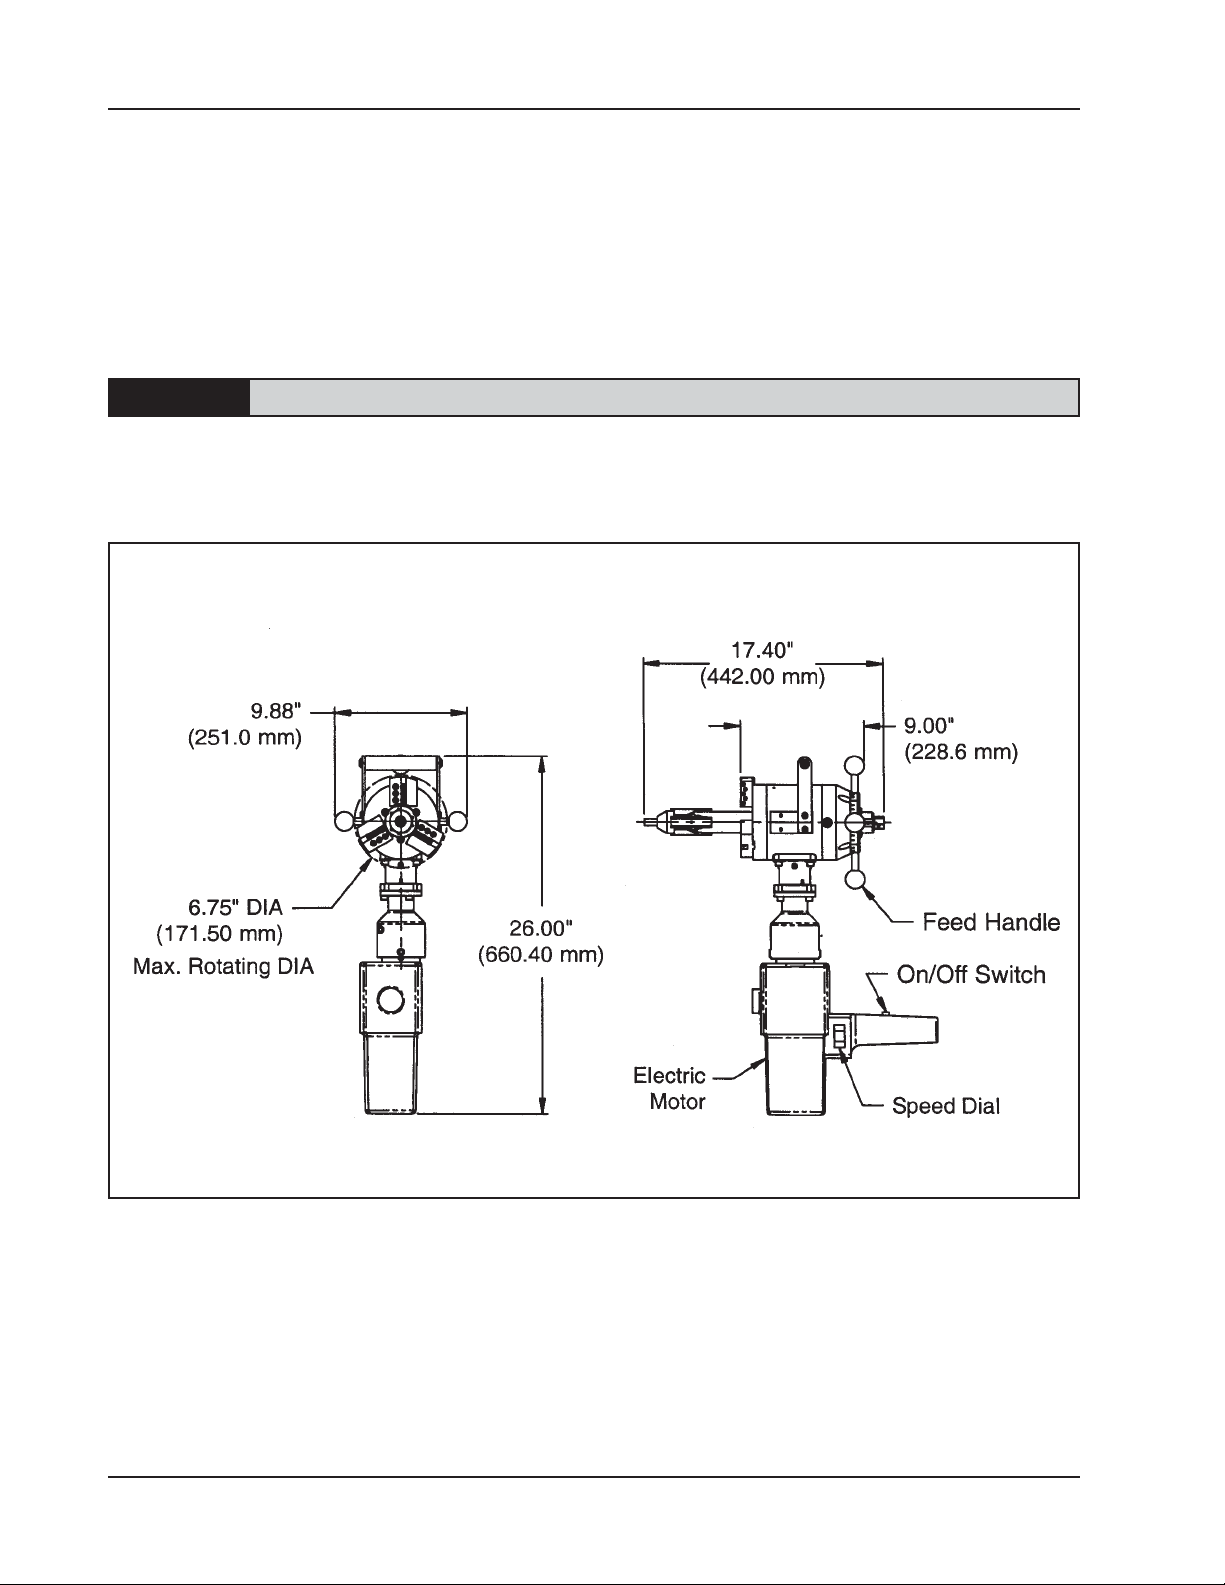
MODEL 206B WITH ELECTRIC MOTOR (110V AC AND 220V AC)
Weight (Less the Mandrel)
34 lbs (16 kg)
Model 206B with an Electric Motor Envelope Drawing
10
92-0211 : Rev. 050224
Page 11
Power Requirements
110V AC, 60Hz or 220V AC, 50 Hz
PIPE CUTTING CAP ACITIES
Basic Pipe Sizes
1 1/2” Pipe Schedules 5 and 10
2” and 2 1/2” Pipe Schedule 5 through 80
3” through 6” Pipe Schedule 5 through 40
Basic Tube Sizes
Up to .280” (7.1 mm) wall tubing with a maximum OD of 6.63” (168.4 mm)
and a minimum ID of 1.63” (41.4 mm) may be beveled with standard procedures.
Model 206B BEVELMASTER™
Wall Thickness Capacity
Wall thickness of all standard pipe schedules, .280” (7.1 mm) max., in the
ranges listed.
Contact TRI TOOL Inc. for heavier wall procedures.
Counterboring Operation
The machine will counterbore pipe and tubing with an ID range of 2.00” (50.8
mm) to 6.41” (162.8 mm).
Material Cutting Capability
Mild steels, chrome steels (Rc 35 max.), stainless steel, copper-nickel and
aluminum without limitations except size and wall thickness as specified
under ‘Wall Thickness Capacity’.
Inconel and some other high temperature alloys may require special procedures as a function of wall thickness and type of end preparation.
Contact the TRI TOOL INC. Engineering Department for details.
Headstock Speeds
92-0211 : Rev. 050224
11
Page 12
TRI TOOL INC.
Maximum Cutting Head Speed 38 rmp
Functional Speed Range 9 to 34 rpm
MODEL 206B WITH ELECTRIC MOTOR, H.D. (HEAVY DUTY)
Weight
NOTE:
less than 60 lbs (27.22 kg)
Power Supply Options
Model 206B with an Electric Motor, H.D. (Heavy Duty) Envelope Drawing
12
92-0211 : Rev. 050224
Page 13
115 VAC, 40 – 60 Hz, 2300 Watt rated Supply
All 115V motors require a minimum of a 20-amp circuit.
230 VAC, 40 – 60 Hz, 2300 Watt Rated Supply
PIPE CUTTING CAP ACITIES
Basic Pipe Sizes
1 1/2” Pipe Schedules 5 and 10
2” and 2 1/2" Pipe Schedules 5 through 160
3” through 6” Pipe All Schedules
Basic Tube Sizes
Model 206B BEVELMASTER™
Up to .875 (22.2 mm) wall tubing with a maximum OD of 6.63” (168.4 mm)
and a minimum ID of 1.63 (41.4 mm) may be beveled with standard mandrel.
Wall Thickness Capacity
Wall thickness of all standard pipe schedules, .875 (22.2 mm) maximum, in
the range listed. Tubing with greater wall thickness may be handled provided
the ID is greater than 1.63” (41.4 mm) and the OD is less than 6.63” (168.4
mm). Contact TRI TOOL Inc. for heavier wall procedures.
Counterboring Operations
The tool will counterbore pipe and tubing with an ID range of 2.00” (50.8 mm)
to 6.41” (162.8 mm).
Material Cutting Capabilities
Mild steels, chrome steels (Rc 35 max.), stainless steel, copper-nickel and
aluminum with out limitations except size and wall thickness as specified in
the previous information.
Inconel and some other high temperature alloys may require special procedures as a function of wall thickness and type of end preparation.
Contact TRI TOOL Inc. Engineering Department for details.
92-0211 : Rev. 050224
13
Page 14
TRI TOOL INC.
Cutting Head Speeds
Maximum Cutting Head Speed 40 rpm
Functional Speed Range 16 - 37 rpm
14
92-0211 : Rev. 050224
Page 15
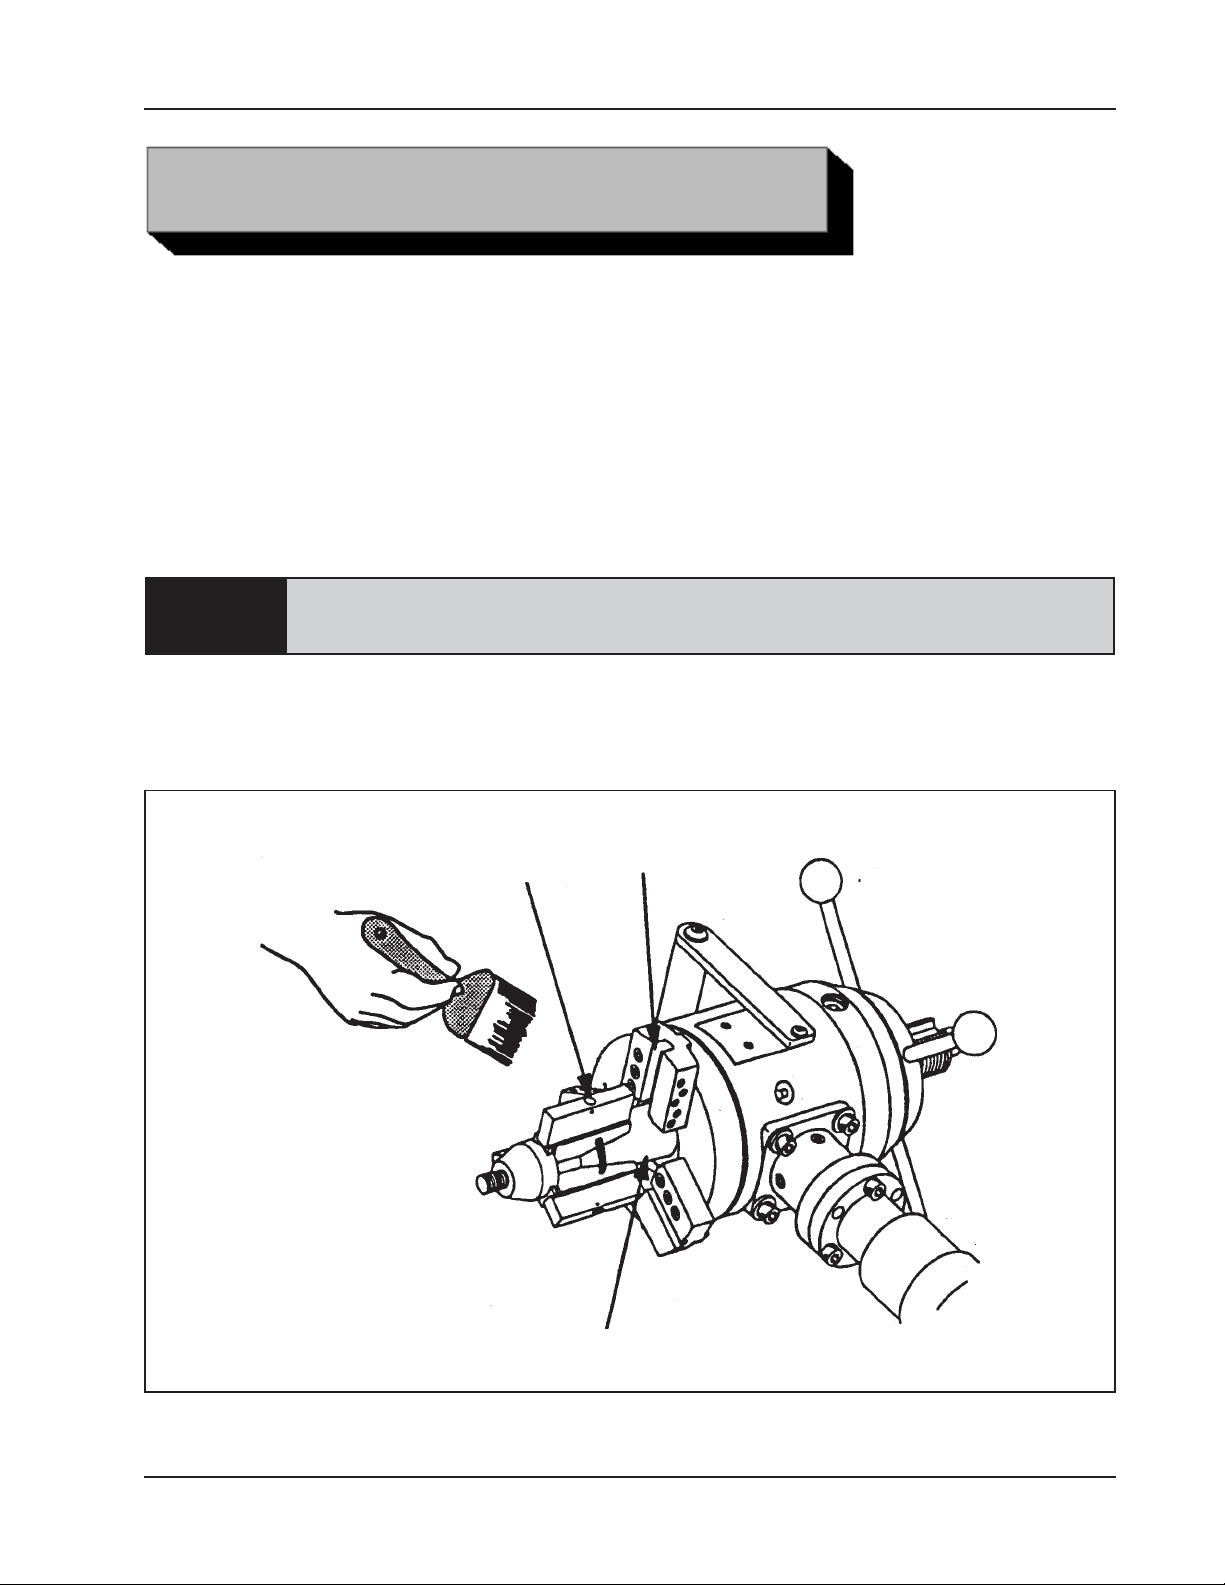
All components should be cleaned and coated with a light film of oil prior to use.
Use a clean, non-detergent oil, preferably SAE 10 (90 SSU) or lighter or oil as specified for the air motor.
AIR SUPPLY
Air Supply for the Model 206B with an air motor requires an adequate filter/regulator/
lubricator (FRL) to be used in the air supply line.
Model 206B BEVELMASTER™
MAINTENANCE
NOTE:
When the Model 206B is operated in the vertical position, cutting head up, it should
be turned upside down and the chips and/or other debris removed after each bevel
has been completed.
The motor warranty is void if damage occurs from contaminated air or lack of
lubrication.
92-0211 : Rev. 050224
15
Page 16
TRI TOOL INC.
Tool life may be severely shortened, unless chips and/or other debris that
NOTE:
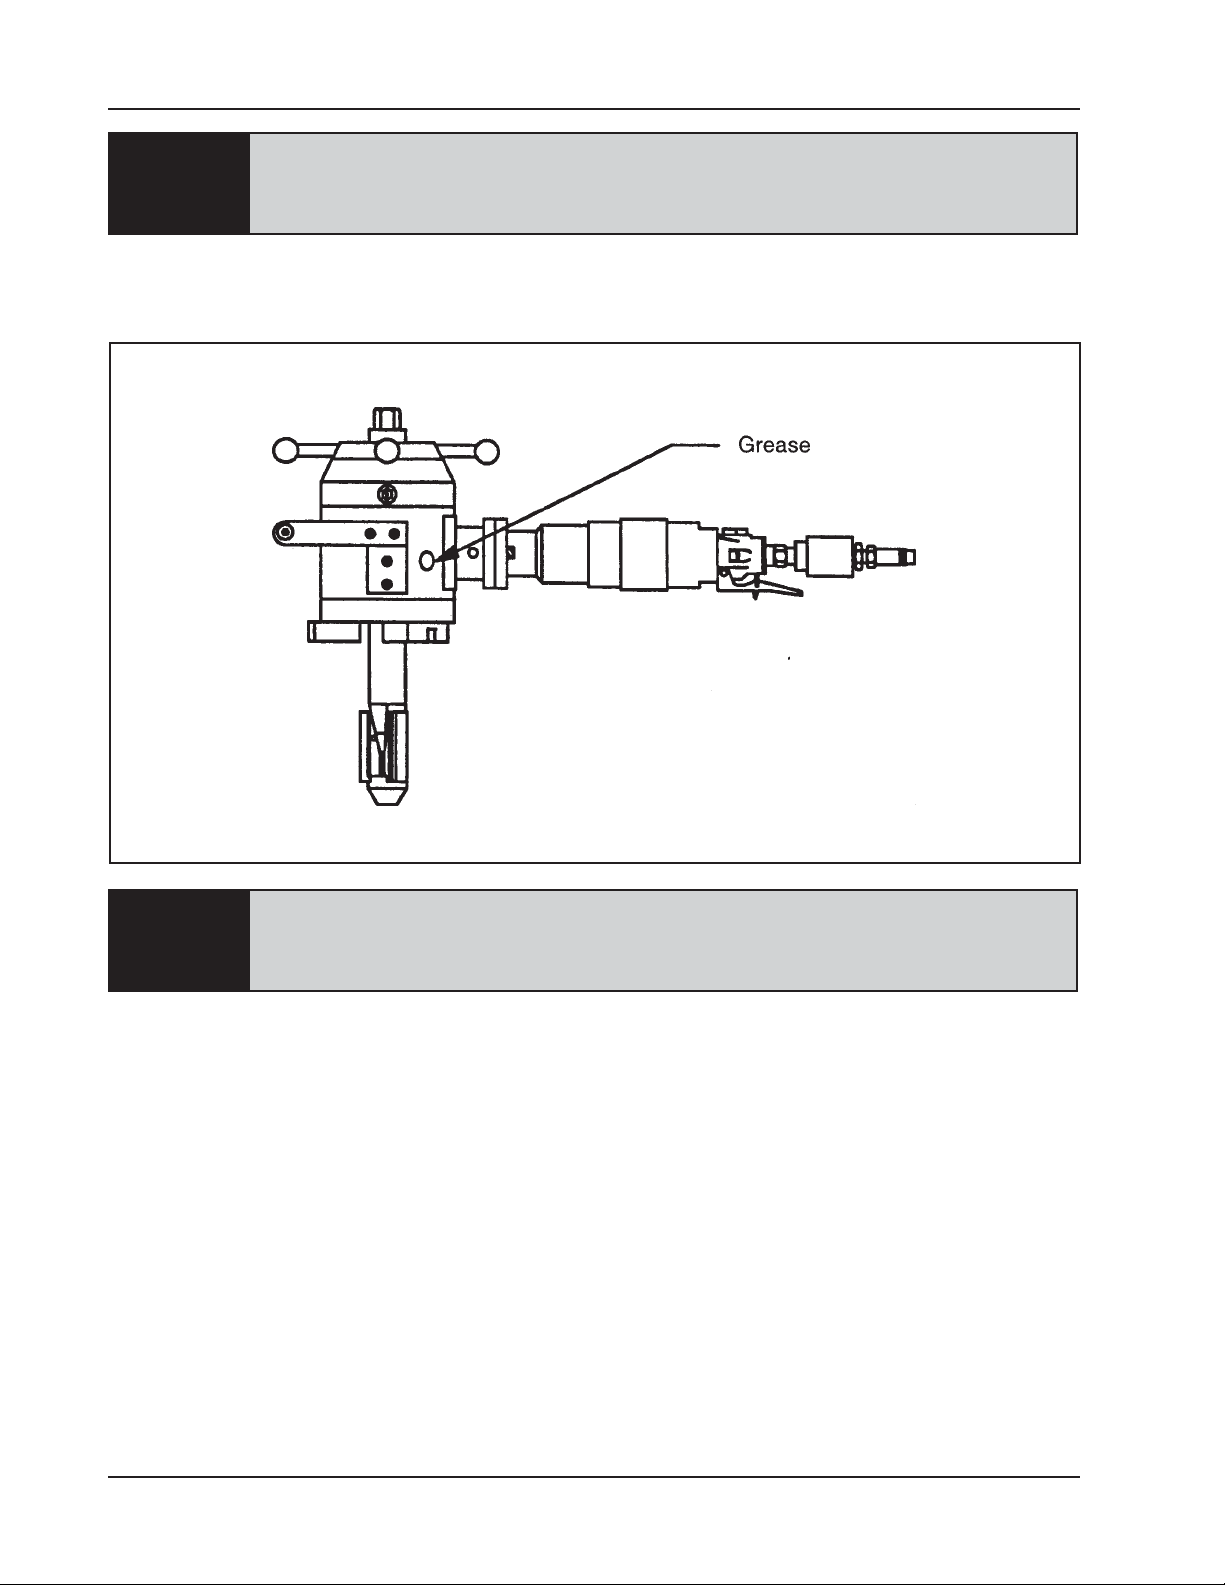
Verify that there is adequate grease in the gear box. Bearing and gears are to be
lubricated using a high string utility grease (P/N 68-0024).
have been deposited on the cutting head during the machining operation are
removed.
Disassembly of a power unit voids the warranty, except when performed by a
NOTE:
TRI TOOL INC. designated repair technician. (A letter of designation is required.)
AIR MOTOR LUBRICATION
No direct maintenance is normally required on the air motor.
However, the air supply must flow through a filter/regulator/lubricator (FRL) unit or
separate units before arriving at the air motor.
The FRL unit must be maintained as required (frequency dependent on the basic air
supply) to keep the water trap drained, filter cleaned and the lubricator oil reservoir
filled so that a drop of oil every 2 to 5 seconds is flowing.
When the Model 206B BEVELMASTER™is to be left idle for 24 hours or more after
being run on ‘wet’ air, it is advisable to squirt oil directly into the air motor inlet and
run the motor for two (2) to three (3) seconds.
16
92-0211 : Rev. 050224
Page 17
This will prevent rusting and freezing of the rotor.
LUBRICANT RECOMMENDA TIONS
The drive gears require a high string lubrication grease such as ‘Chevron Ultra-Duty
Grease EP NCG12’ (P/N 68-0024).
The air motor requires a Class 2 lubricant, viscosity of 100 to 200 SSU at 100° F
(38° C) minimum aniline point of 200° F (93° C).
TRI TOOL INC. Air Tool Lubricant (P/N 68-0022)
• AMOCO – American Industrial Oil No. 32
• Atlantic Richfield – Duro Oil S-150
• Chevron – A.W. Machine Oil 32
• Exxon – Nuto H32
• Shell – Tellus Oil 32
Model 206B BEVELMASTER™
The bearings in the air or electric motor are sealed and do not require any lubrication.
92-0211 : Rev. 050224
17
Page 18
TRI TOOL INC.
Read the operating instructions carefully before attempting to operate the Model
206B.
Use eye protection at all times when operating the Model 206B.
Select the recommended jaw blocks and/or ramp set for the pipe size to be machined. (Refer to the jaw block selection chart.)
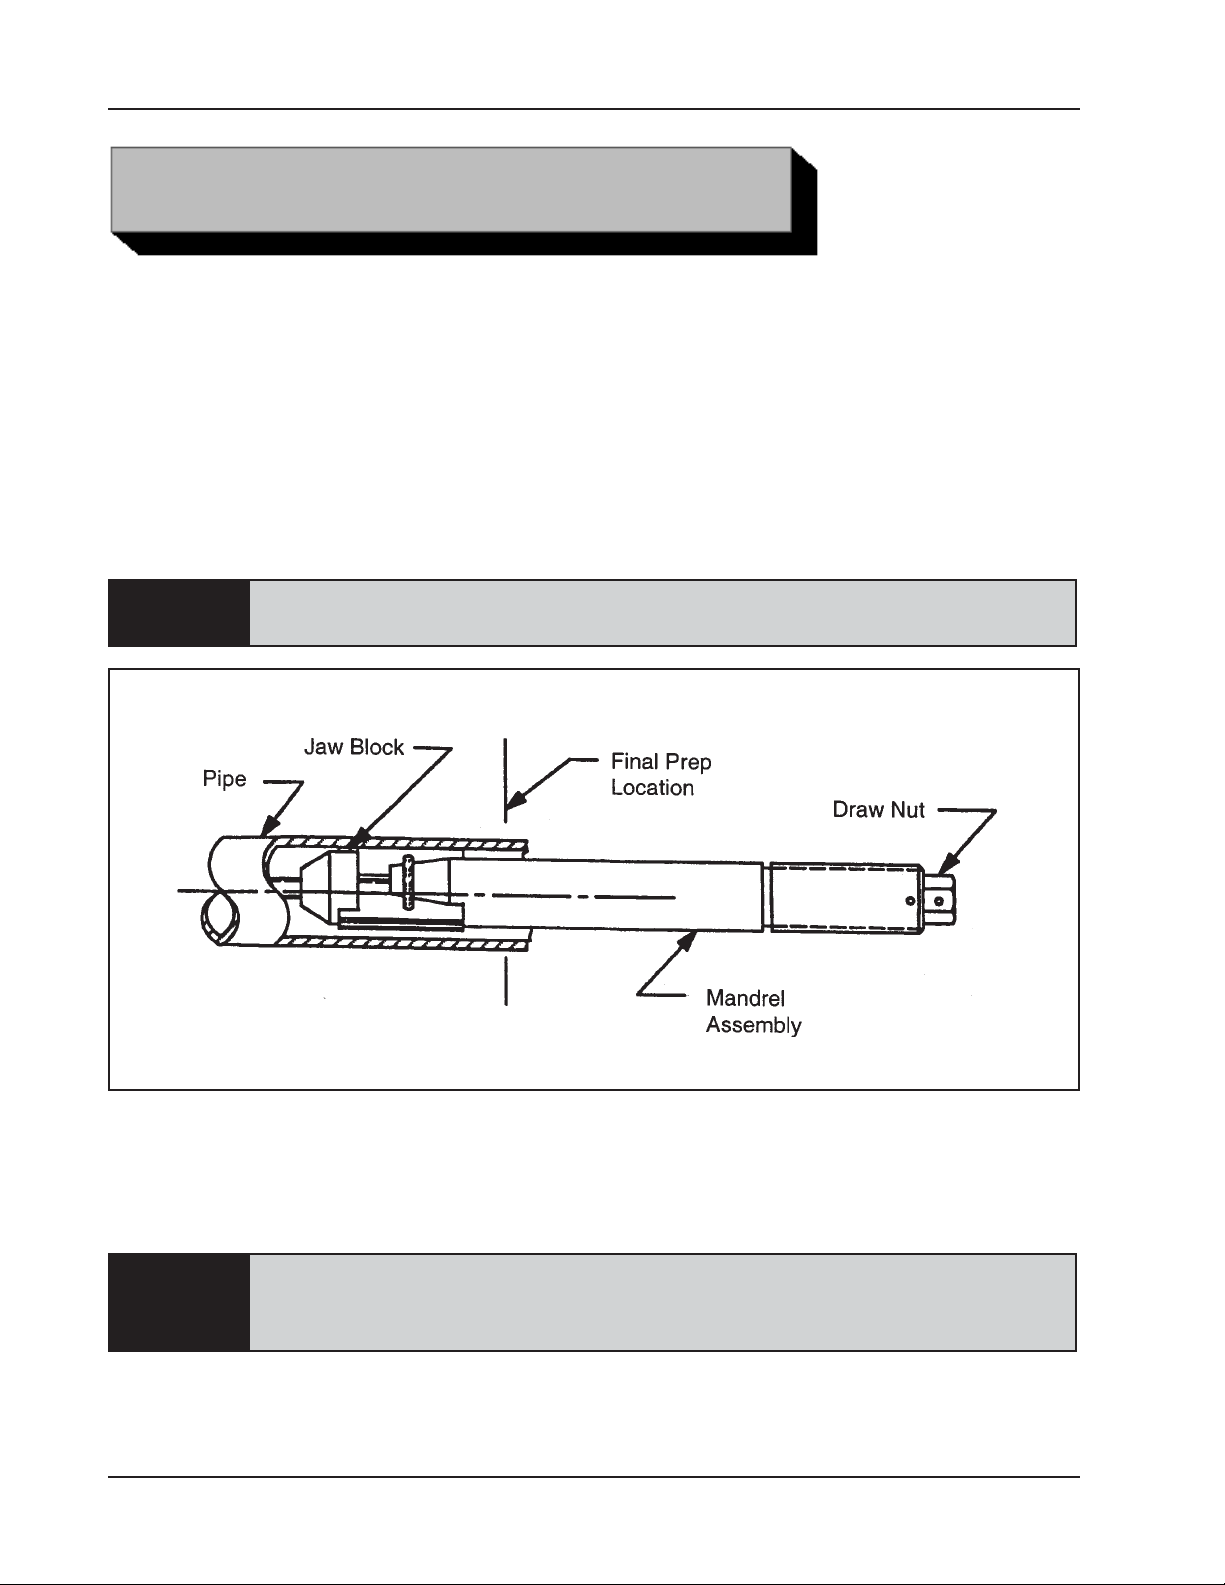
Install the mandrel assembly into the pipe.
OPERATION
NOTE:
Tighten the draw nut to force the jaw blocks out to the inside diameter of the pipe or
tube.
In order to avoid cutting the jaw blocks during the machining operation, the
mandrel must be installed beyond the final end preparation location.
Select the tool bit(s) required to machine the pipe to the configuration desired.
WARNING:
When performing any multiple machining operation such as facing, beveling, and/or
counterboring, the counterbore tool bit should be installed to ‘lead’ the bevel tool bit.
18
Use of dull or improperly designed tool bits or tool bits not manufactured by
TRI TOOL INC. may result in poor performance and may constitute abuse of
this machine and therefore voids the TRI TOOL INC. factory warranty.
92-0211 : Rev. 050224
Page 19
Model 206B BEVELMASTER™
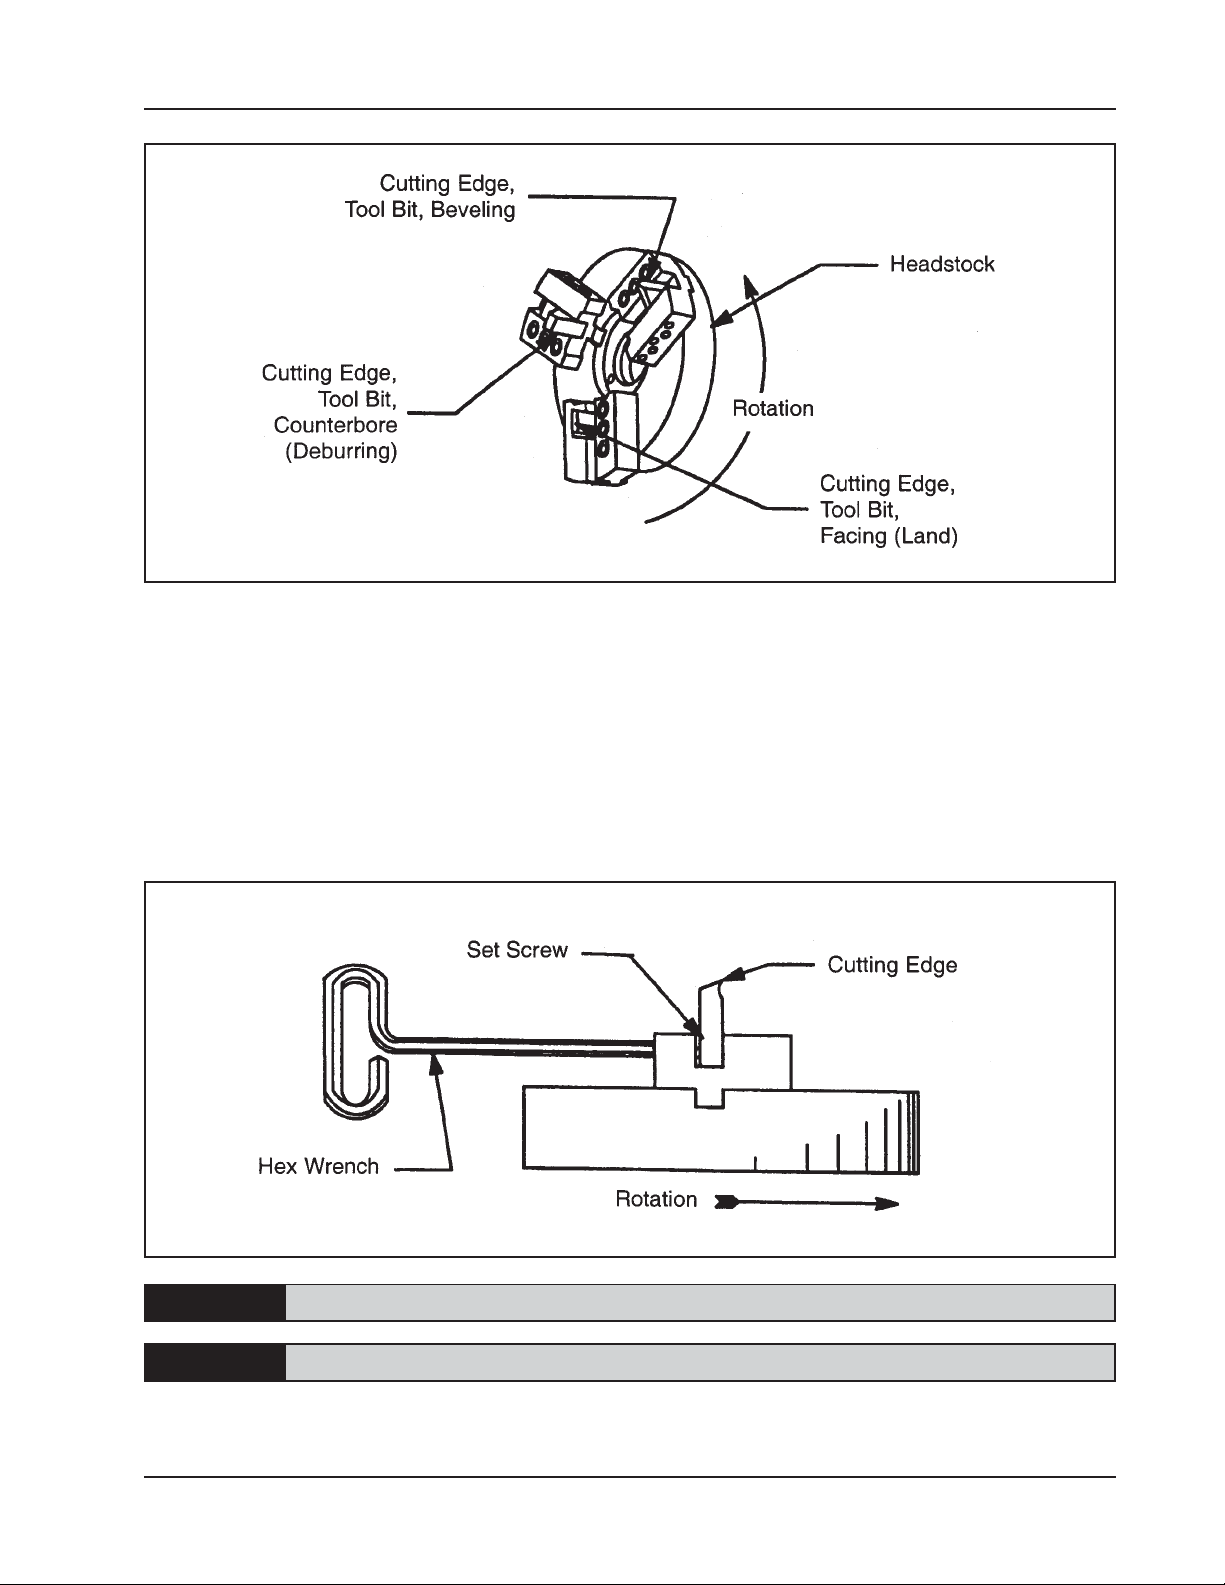
Attach the tool holders in the appropriate position for the size of pipe being machined.
Use the four (4) outer holes for the larger diameters of pipe.
Use the four (4) inner holes for the smaller diameters of pipe.
Insert the tool bit(s) into the slot(s) in the tool holder(s).
CAUTION:
CAUTION:
The cutting edge of the tool bit(s) must be located on the radial centerline.
Insure that no tool bit is installed backwards.
92-0211 : Rev. 050224
19
Page 20
TRI TOOL INC.
Tighten the set screws to secure the tool bit(s) to the tool holder(s).
Adjust the counterbore tool bit radially to control counterbore diameter.
Adjust the bevel tool bit radially to control the counterbore depth to the bevel relationship.
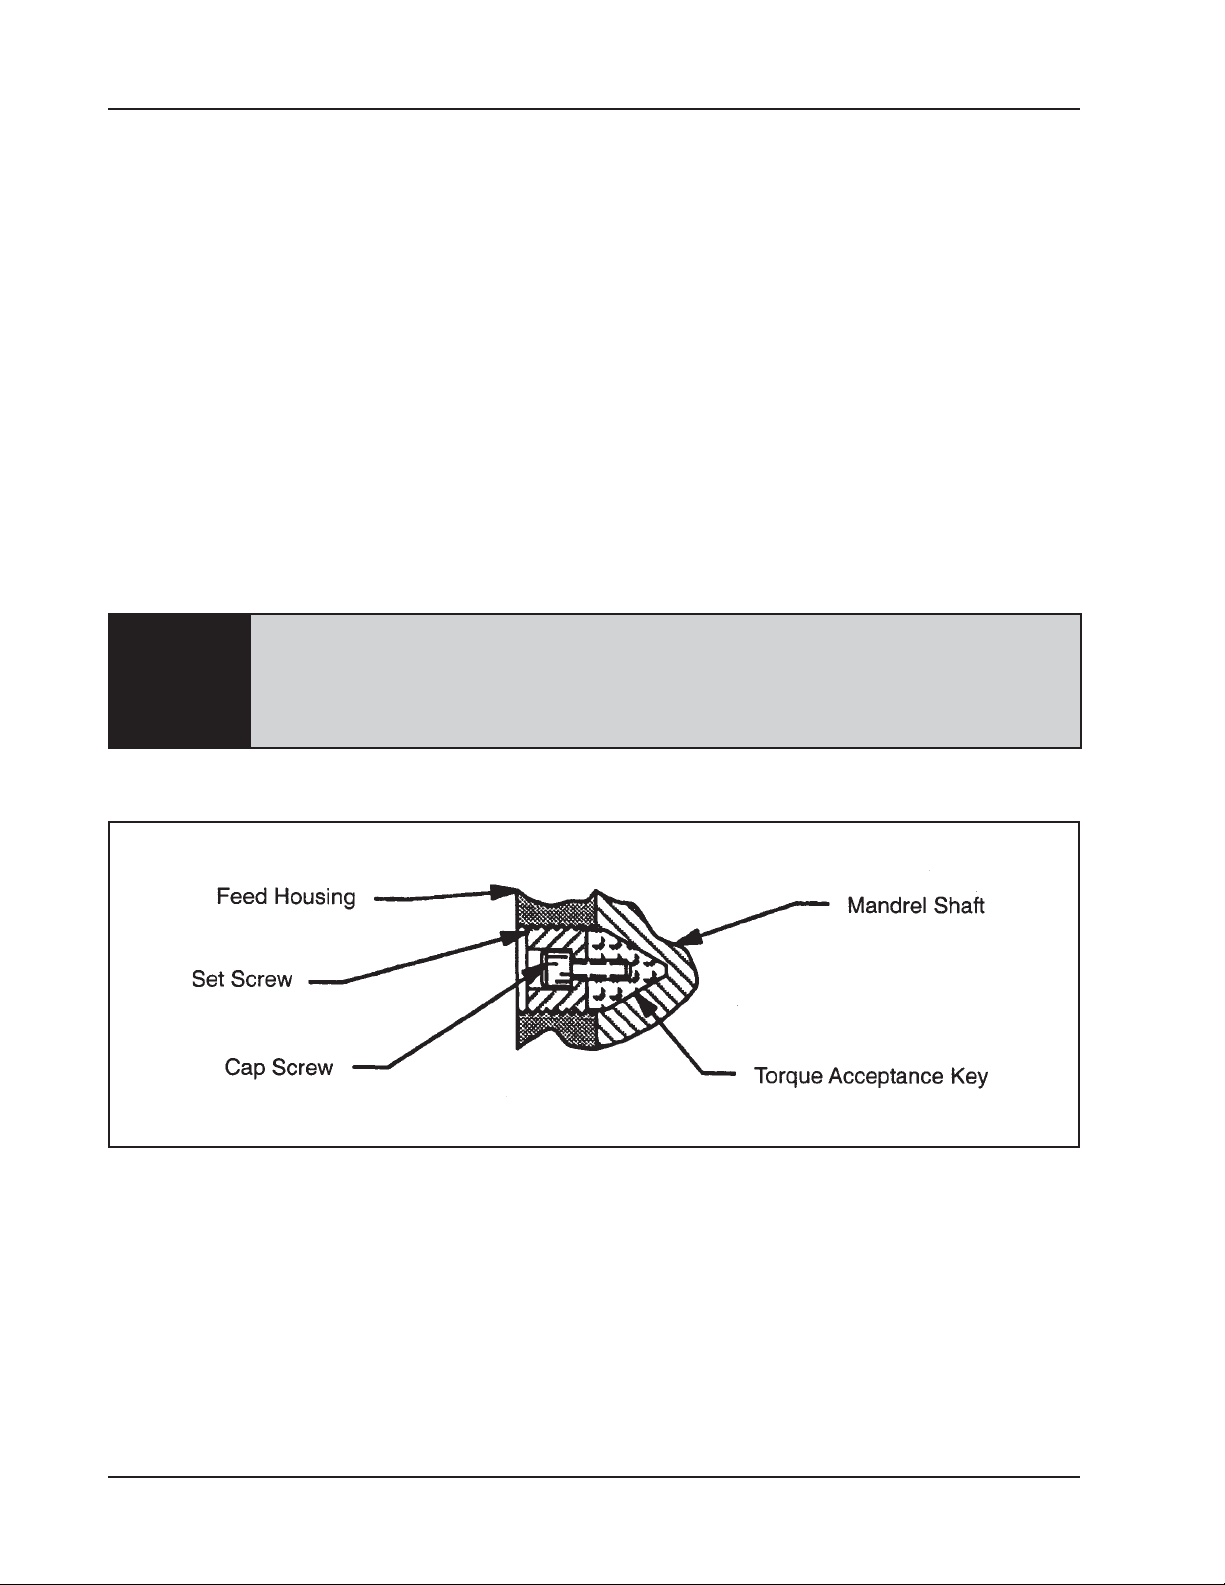
Slide the Model 206B gently onto the mandrel assembly until it comes to a solid stop
against the torque acceptance keys.
The Model 206B with the mandrel assembly installed maybe mounted to the pipe as
one unit.
Rotate the Model 206B as required to engage the torque acceptance keys with the
slots in the mandrel shaft.
Since the mandrel shaft will contact the torque acceptance keys before the
NOTE:
feed nut engages the mandrel shaft threads, caution should be taken not to
force (or allow) the machine to impact the lead threads of the feed nut with
the lead threads of the Mandrel.
ADJUSTMENT OF THE TORQUE ACCEPTANCE KEYS
Adjustment of the torque acceptance keys will be required if the BEVELMASTER™
is loose radially on the mandrel shaft.
This may appear as chatter in the tool bit.
Loosen the cap screws in both torque acceptance keys.
20
Rotate the set screw as required until the torque acceptance keys are riding snugly
in the slots in the mandrel shaft.
92-0211 : Rev. 050224
Page 21
Model 206B BEVELMASTER™
Run the Feed in and out to insure that the torque acceptance keys are not so tight
that the feed is impaired.
Re-tighten the cap screws to retain the new settings.
Rotate the feed handle clockwise to engage the feed nut with the thread on the
mandrel shaft.
WARNING:
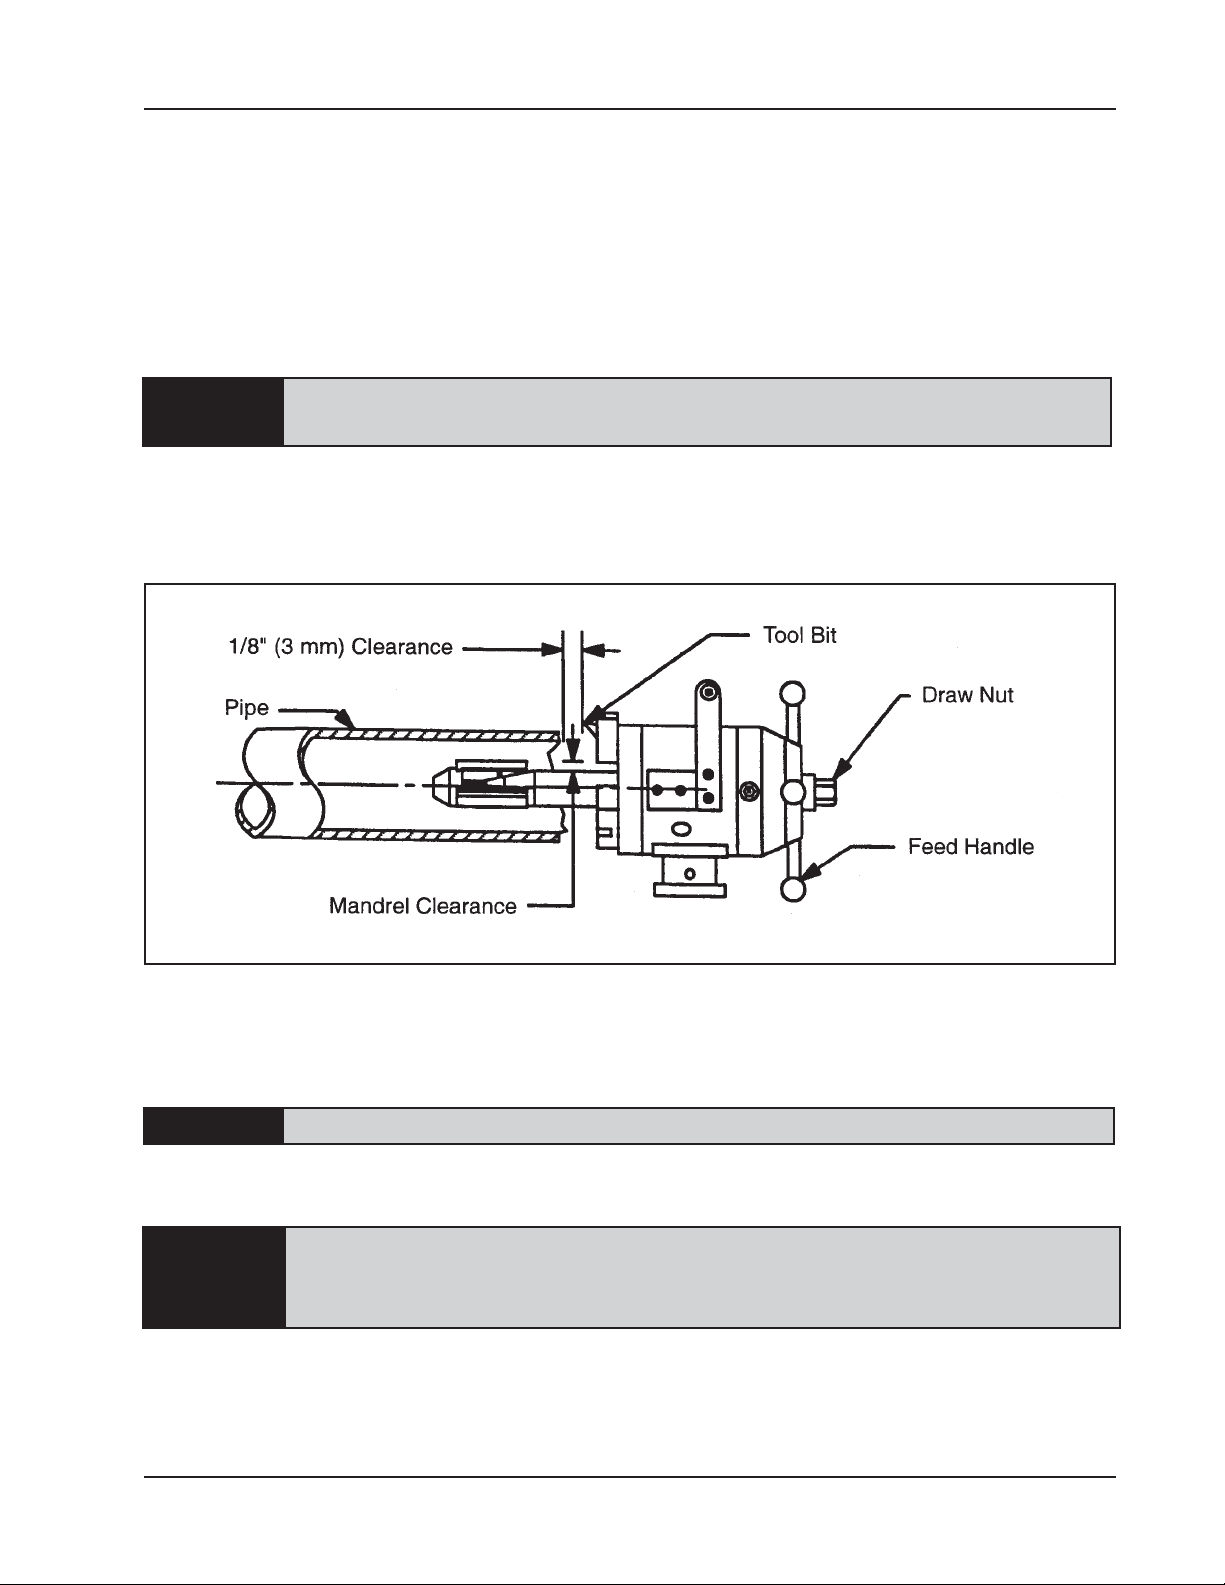
Verify a clearance of 1/8” (3 mm) minimum between the tool bit and the pipe face.
Make sure that there is a clearance between the tool bit(s) and the mandrel.
A minimum of ten (10) threads must be engaged to prevent thread strippage
during the machining operation.
Air Motor: Attach the proper air supply line to the Model 206B.
Electric Motor: Plug the power cord into the proper outlet.
NOTE:
Check that the filter/regulator/lubricator (FRL) is installed and set properly.
MACHINING OPERA TION
Do Not Override the Deadman Switch on the Unit. Locking down, obstructing,
WARNING:
or in any way defeating the deadman switch on this unit may result in serious
injury.
Air Motor
Depress the air motor trigger.
92-0211 : Rev. 050224
21
Page 22
TRI TOOL INC.
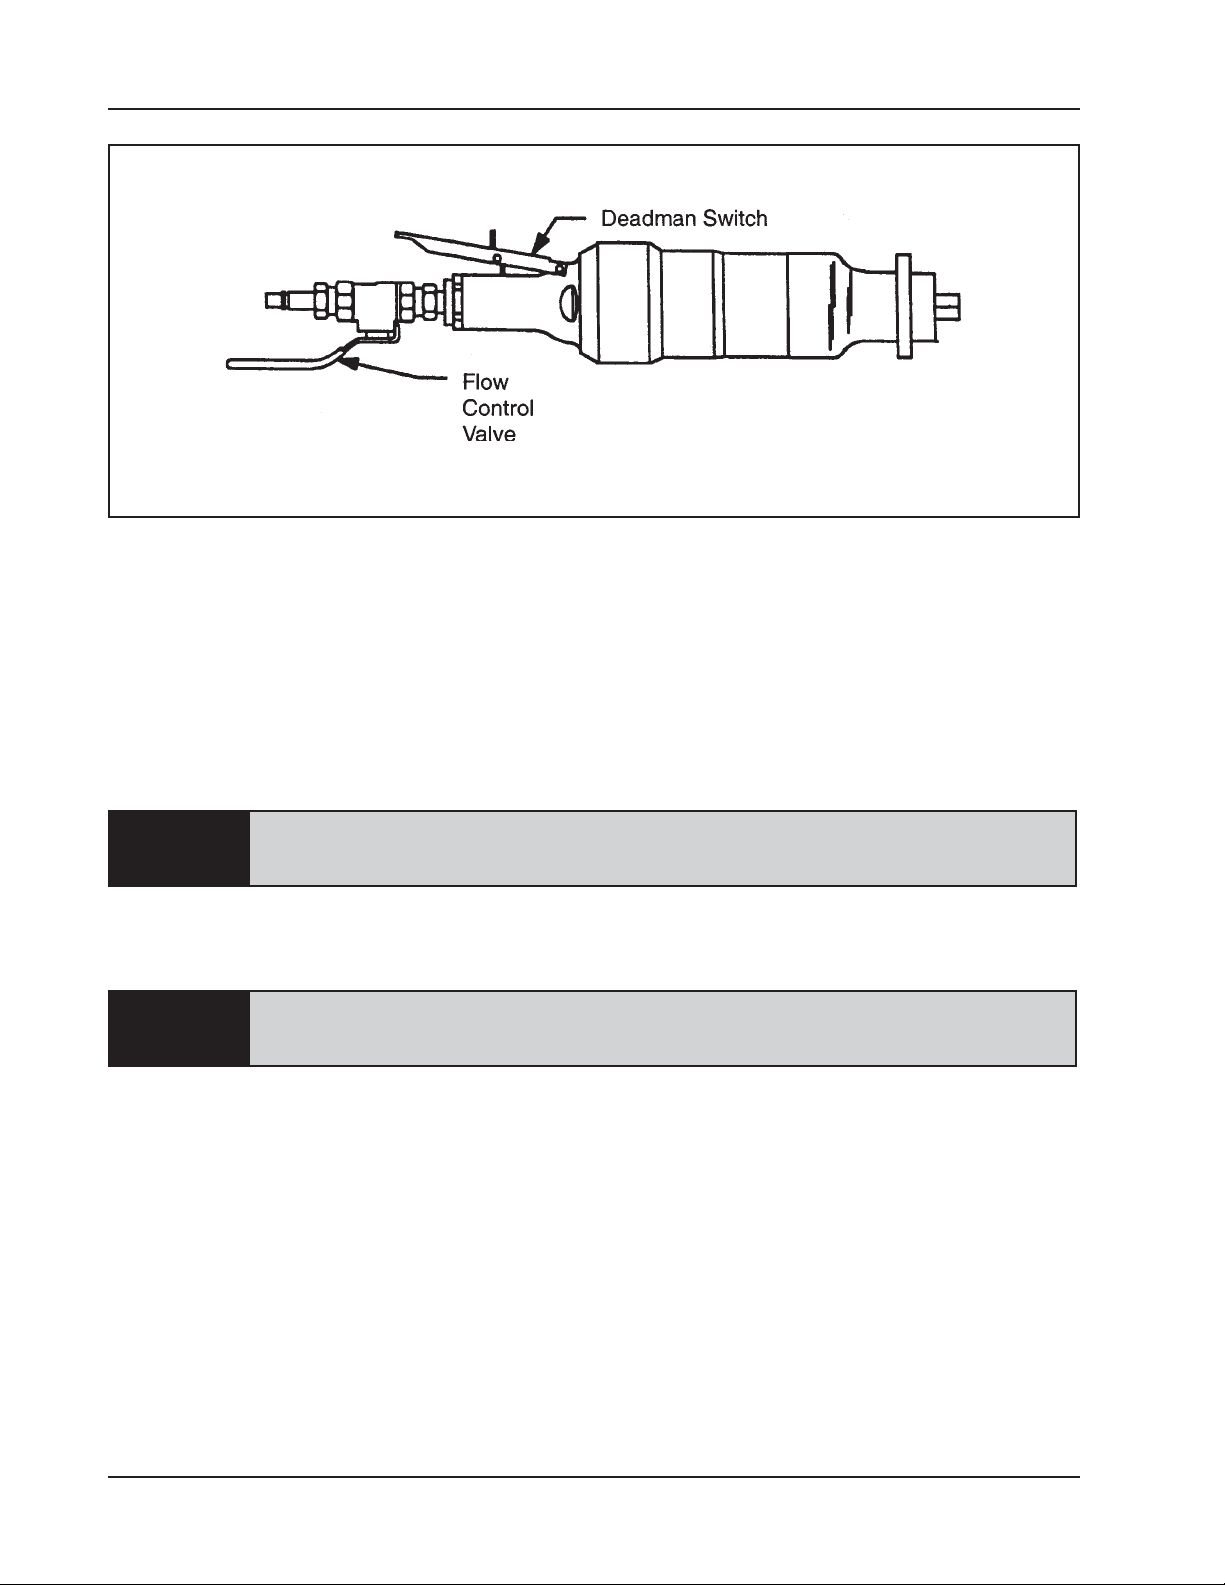
Adjust the cutting speed by rotating the flow valve at the air connection.
Electric Motor
CAUTION:
WARNING:
Depress the trigger.
Adjust the cutting speed by rotating the speed control dial on the trigger and/
or using the high/low switch.
Do not change the high/low switch while the motor is running. Damage to the
gears may occur.
Rotate the feed handle clockwise to bring the tool bit(s) and pipe closer together.
The actual machining operation will begin when the first tool bit contacts the
pipe.
When the pipe end is not square to the pipe axis, the tool bit will contact only a small segment of the pipe during each revolution.
To avoid tool bit damage, the feed rate should be very slow until the tool bit(s)
is in contact with the pipe continually during at least one full revolution.
22
Continue rotating the feed handle clockwise until the end of the pipe is completely machined.
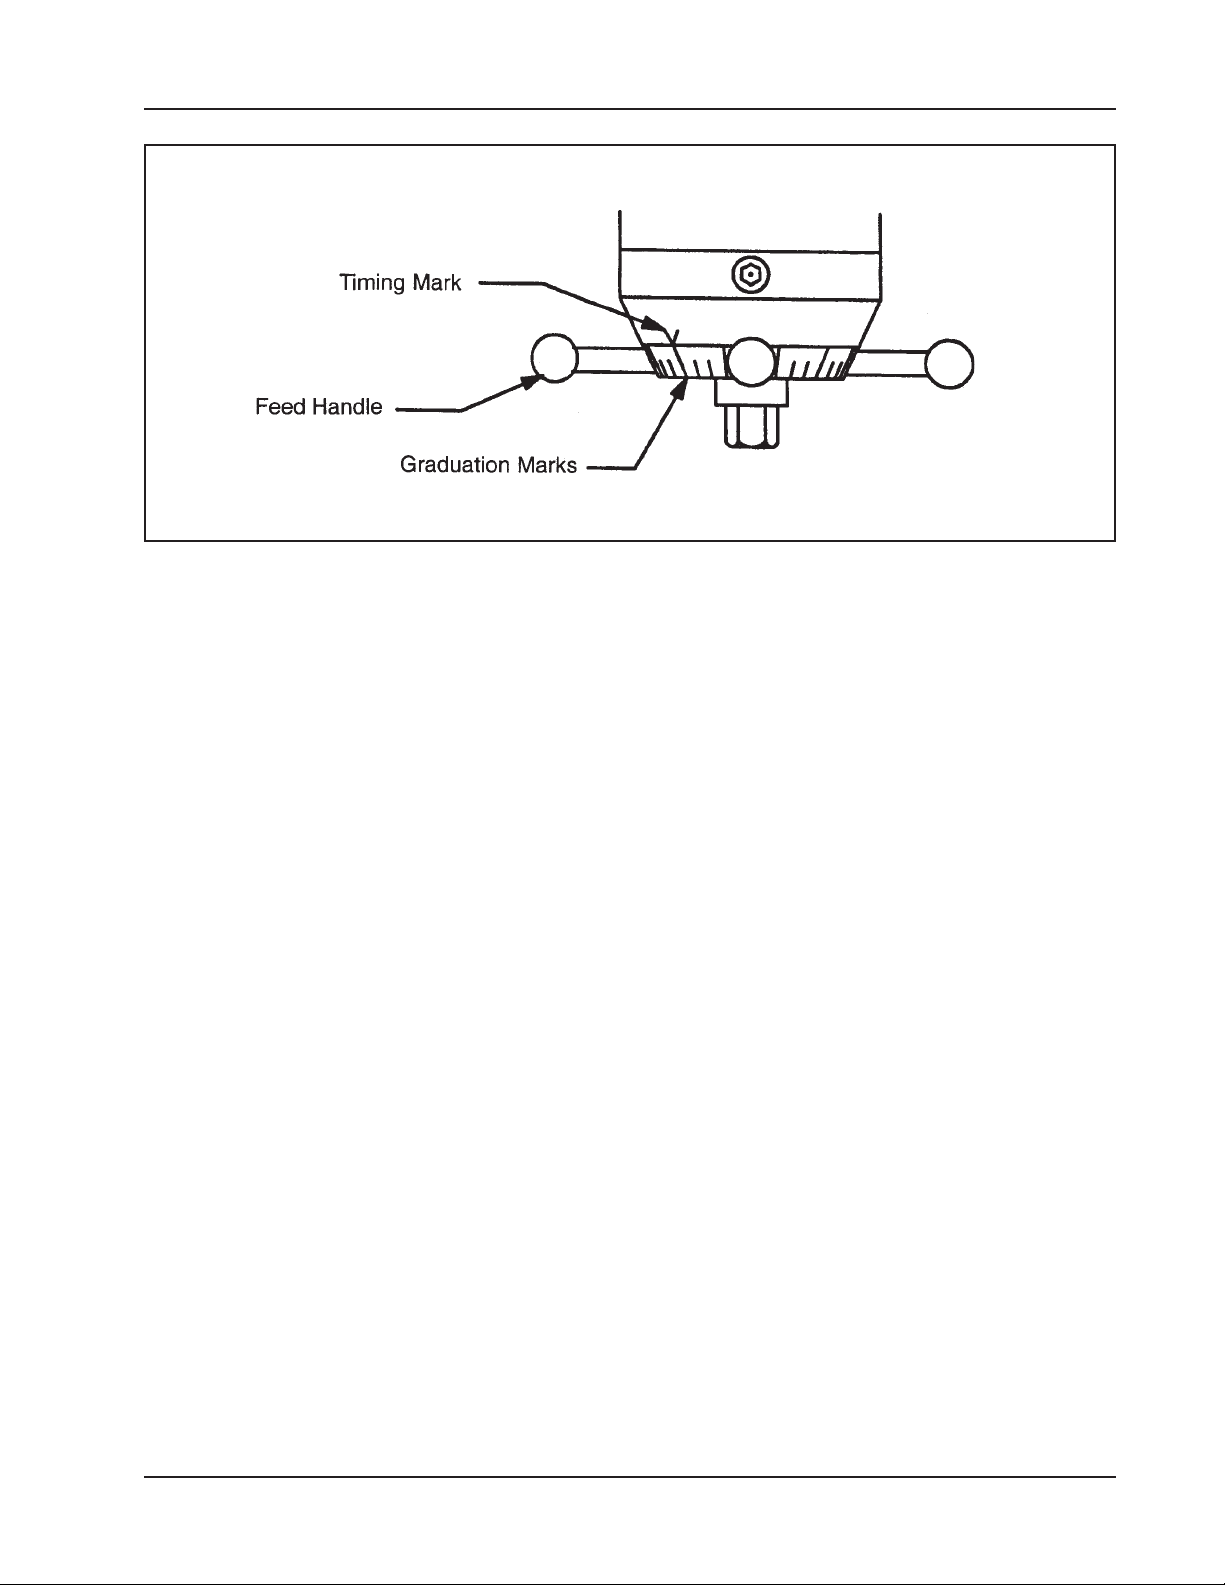
The axial feed rate of the tool bit is .0023” (.06 mm) for each graduation or
.083” (2.11 mm) for each complete revolution of the feed handle.
92-0211 : Rev. 050224
Page 23
Model 206B BEVELMASTER™
Discontinue feed and allow the head to rotate one (1) to three (3) revolutions
to improve the finish of the prep surface.
Release the trigger to stop the head rotation.
Rotate the Feed Handle counterclockwise to separate the Tool Bit(s) from the
pipe.
Rotate the feed handle counterclockwise until the tool bit is 1/8” (3 mm)
minimum from the end of the pipe or tube.
Loosen the draw nut on the mandrel to release the mandrel from the pipe.
The mandrel assembly may be left in the Model 206B and installed as a
complete assembly.
92-0211 : Rev. 050224
23
Page 24
TRI TOOL INC.
CUTTING SPEEDS AND FEEDS
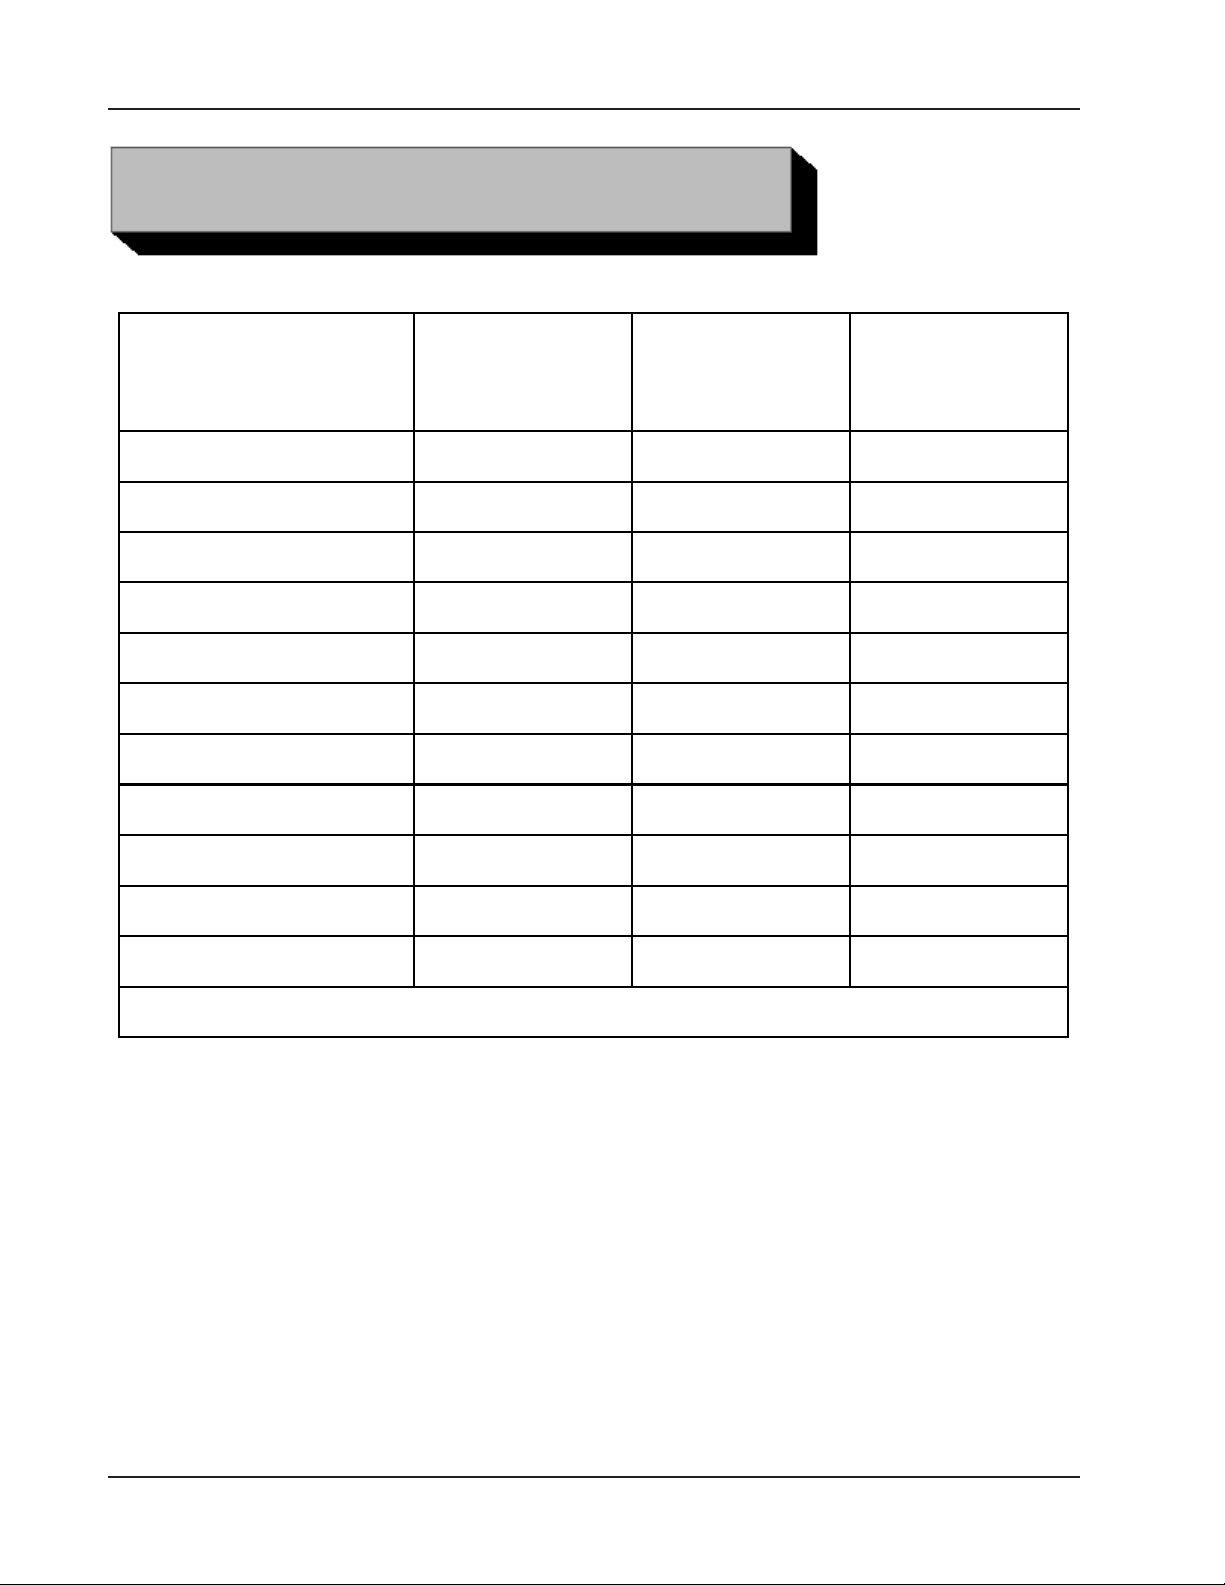
Nominal
Cutting DIA
1.50" (38.1 mm) 42 53 64
2.00" (50.8 mm) 32 40 48
2.50" (63.5 mm) 25 32 34
3.00 (76.2 mm) 21 27 32
3.50" (88.9 mm) 18 23 27
4.00" (101.6 mm) 16 20 24
4.50" (114.3 mm) 14 18 21
5.00" (127.0 mm) 13 16 19
5.50" (139.7 mm) 12 15 17
6.00" (152.4 mm) 11 13 16
RPM for
200 in/min
(5080 mm/min)
RPM for
250 in/min
(6350 mm/mi n )
RPM for
300 in/min
(7620 mm/min)
6.50" (165.1 mm) 10 12 15
Cutting Speed (Approximately)
Use 200 surface inches per minute (5080 surface millimeters per minute) for:
Stainless steels in general when no coolant is allowed, all heavy-wall tube
and some chrome/molybdenum steels.
Use 250 surface inches per minute (6350 surface millimeters per minute) for:
Mild steels and some thin-wall stainless steels when coolants are permitted
and applied.
Use 300 surface inches per minute (7620 surface millimeters per minute) for:
Aluminum and some thin-wall mild steel and tube with coolants.
24
92-0211 : Rev. 050224
Page 25
BASIC FEED RECOMMENDATION
Use very light feed for initial beveling or until a continuous cut is established.
This is very important for longer tool bit life when cutting through flame cut or
out of square pipe ends.
Use adequate feed, .003” (.08 mm) to .006” (.15 mm) per revolution thereafter, to
establish a continuous chip cut.
If the feed is too light, only light stringer chips will be removed.
If the feed is too heavy the drive will start to overload and the chip will start to
have a rough or torn appearance.
Stainless steel, which work hardens, must be worked with heavy enough feed to stay
under the work hardened surface, .003" (.08 mm) to .006" (.15 mm) feed.
Model 206B BEVELMASTER™
Never allow the Tool Bit to burnish the surface.
Reduced feeds and speeds will normally minimize chatter problems.
92-0211 : Rev. 050224
25
Page 26
TRI TOOL INC.
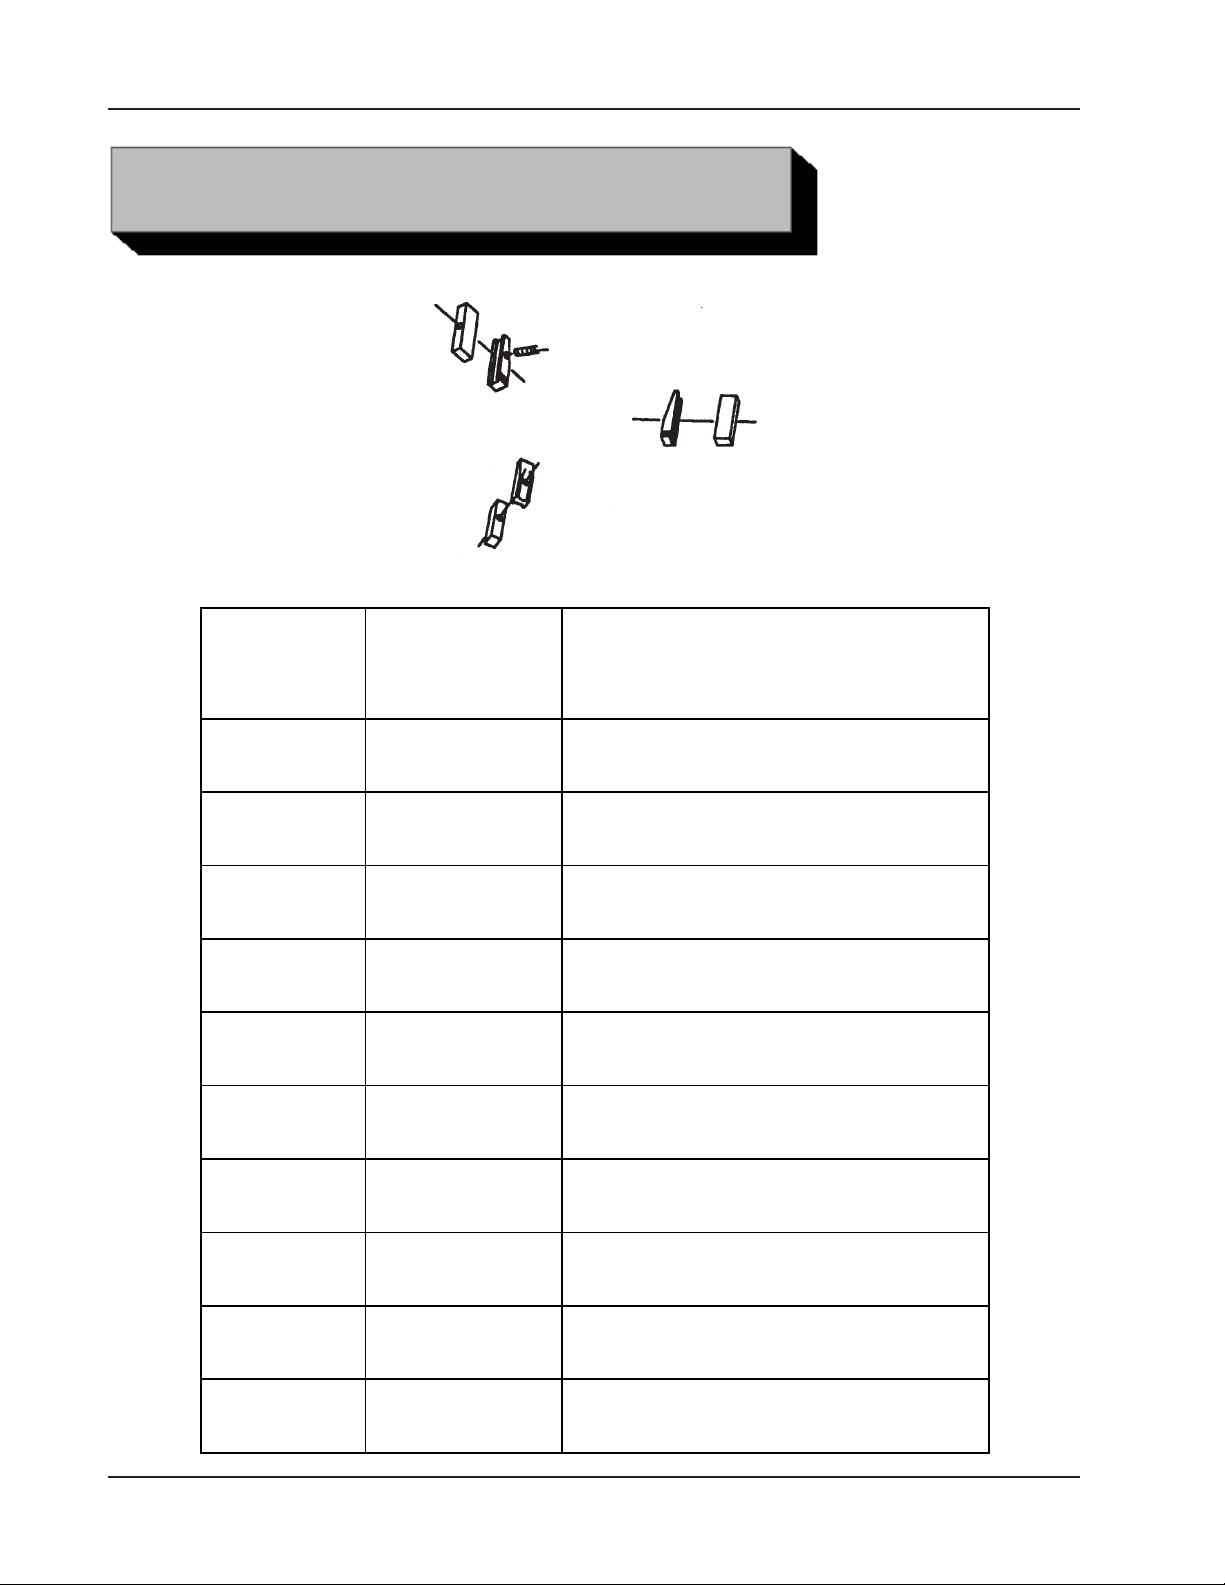
JA W BLOCKS AND RAMPS
ID
RAMP
SET
Standard Not Required
Standard 08-0162
Standard 08-0163
Standard 08-0164
Standard 08-0165
Extended Not Required
Extended 08-0162
BLOCK
P/N
MOUNTING
RANGE
1.63" to 2.18" ID
(41.4 mm to 55.4 mm ID)
2.08 " to 2.65" ID
(52.8 mm to 67.3 mm ID)
2.55" to 3.12" ID
(64.8 mm to 79.2 mm ID)
3.02" to 3.60" ID
(76.7 mm to 91.4 mm ID)
3.50" to 4.08" ID
(88.9 mm to 103.6 mm ID)
3.98" to 4.55" ID
(101. 1 mm to 115.6 mm ID)
4.47" to 5.05" ID
(113. 5 mm to 128.3 mm ID)
26
Extended 08-0163
Extended 08-0164
Extended 08-0165
4.95" to 5.53" ID
(125. 7 mm to 140.5 mm ID)
5.43" to 6.01" ID
(137. 9 mm to 152.7 mm ID)
5.91" to 6.49" ID
(151. 1 mm to 164.8 mm ID)
92-0211 : Rev. 050224
Page 27
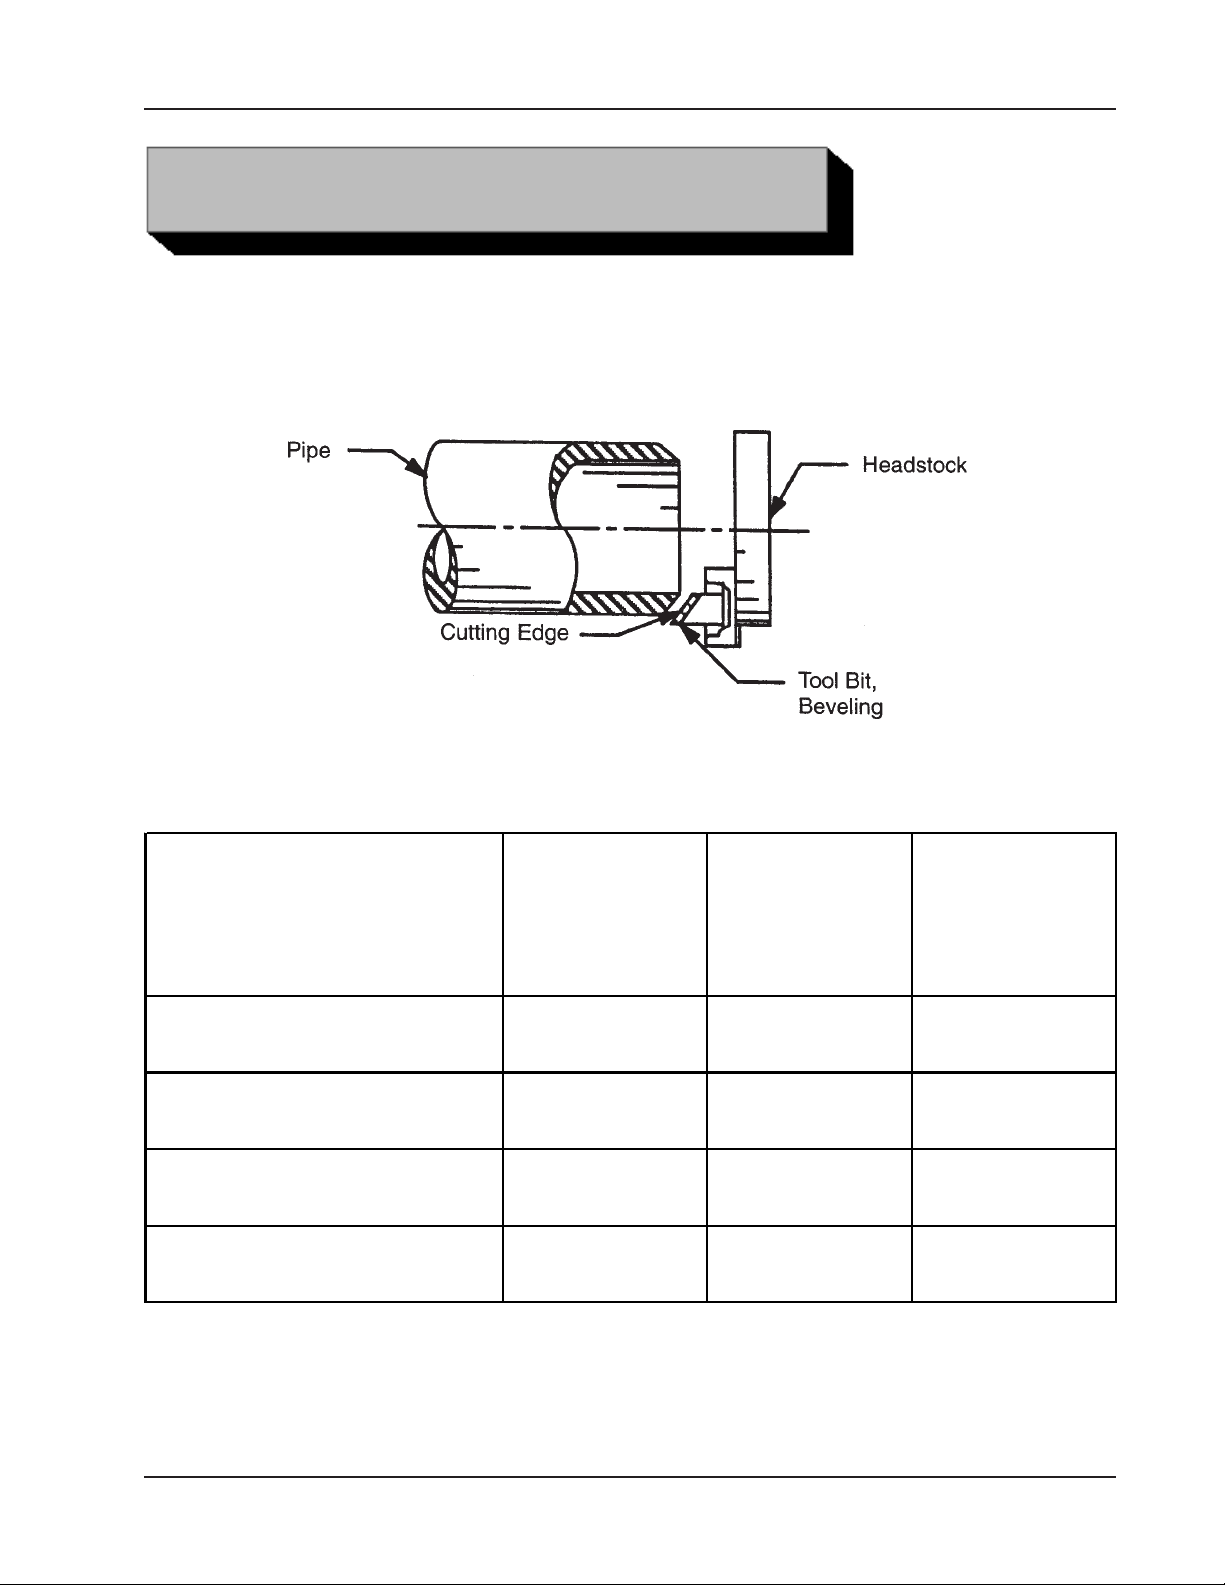
TOOL BITS
TOOL BIT, BEVELING
Model 206B BEVELMASTER™
ID
Range
2.223" thru 5.500"
(56.5 mm thru 139. 7 mm)
2.203" thru 5.500"
(56.0 mm thru 139. 7 mm)
2.750" thru 6.400"
(69.9 mm thru 162. 6 mm)
2.937" thru 6.400"
(74.6 mm thru 162. 6 mm)
Pipe
37.5°
Beveling
or Tube
Tool Bit
Tool Bit
Material
P/N
CS 99-2905 99-2904
SS 99-2918 99-2917
CS 99-2906 99-2904
SS 99-2919 99-2917
Facing
P/N
92-0211 : Rev. 050224
27
Page 28
TRI TOOL INC.
TOOL BIT, BEVELING
ID
Range
2.046" thru 5.312"
(52.0 mm thru 134. 9 mm)
2.046" thru 5.312"
(52.0 mm thru 134. 9 mm)
3.078" thru 6.344"
(78.2 mm thru 161. 1 mm)
3.078" thru 6.344"
(78.2 mm thru 161. 1 mm)
Pipe
FAcing
Beveling
45°
or Tube
Tool Bit
Tool Bit
Material
P/N
CS 99-2913 99-2904
SS 99-2926 99-2917
CS 99-2914 99-2904
SS 99-2927 99-2917
P/N
28
92-0211 : Rev. 050224
Page 29
Model 206B BEVELMASTER™
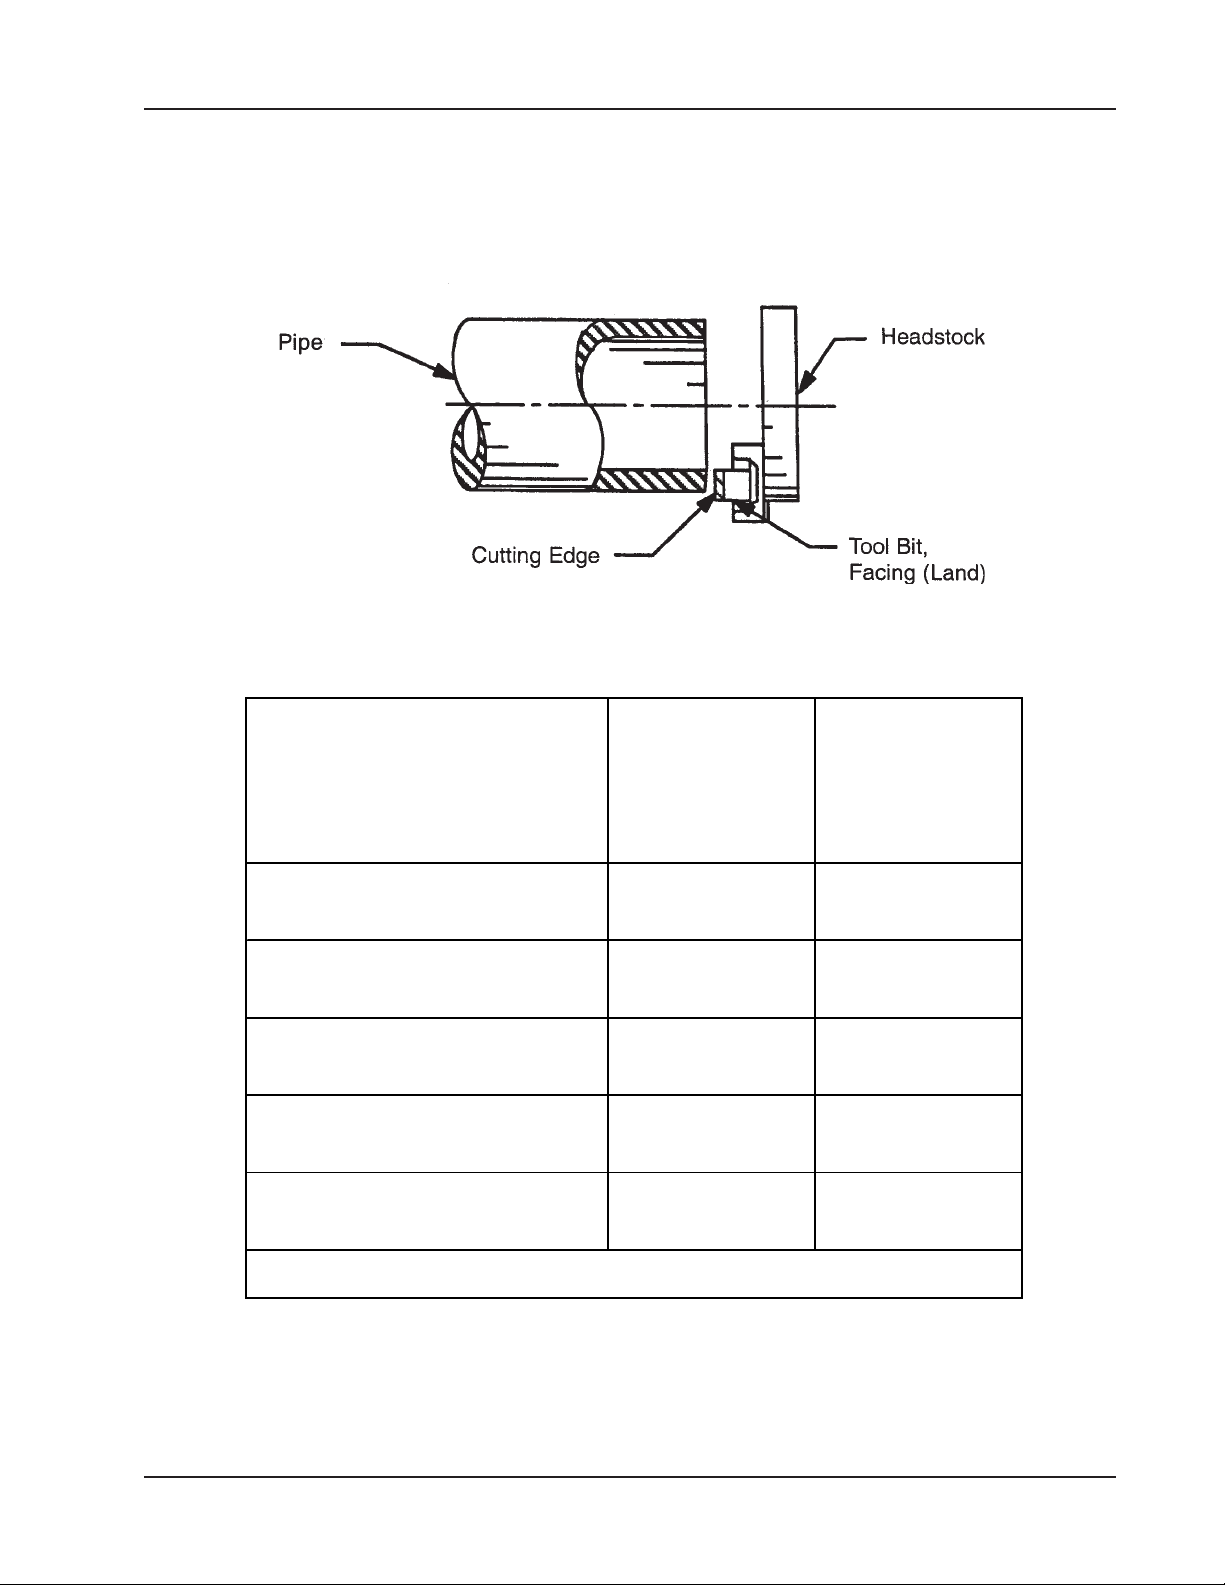
TOOL BIT, FACING (LAND)
OD
Pipe
or T ube
Range
Material
1.625" thru 6.750"
(41.3 mm thru 171.5 mm)
1.625" thru 6.750"
(41.3 mm thru 171.5 mm)
1.625" thru 6.750"
(41.3 mm thru 171.5 mm)
1.625" thru 6.750"
(41.3 mm thru 171.5 mm)
1.625" thru 6.750"
(41.3 mm thru 171.5 mm)
* Cobalt High Heat Tool Bits ar e available.
CS
SS
CS
SS
SS 99-2917
SS 99-2979*
COPP ER 99-4537
Facing
(Land)
T ool Bit
P/N
99-0135
99-2904
92-0211 : Rev. 050224
29
Page 30
TRI TOOL INC.
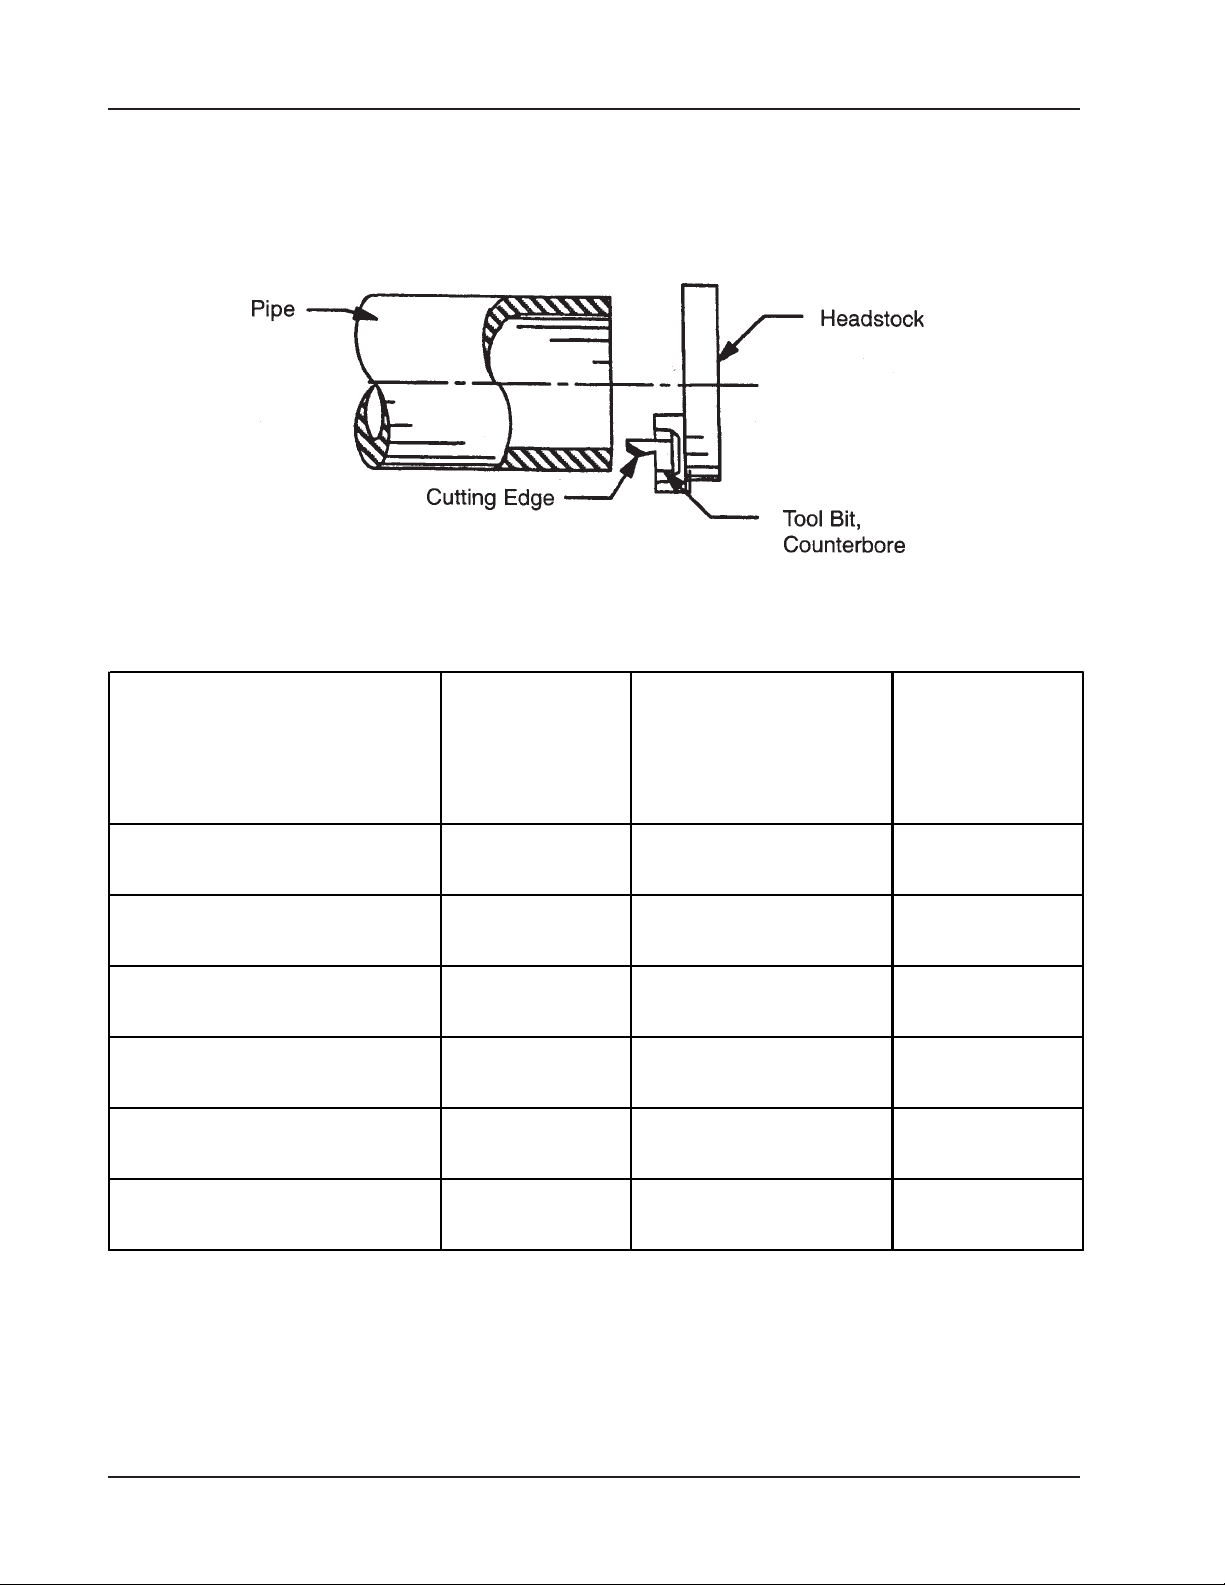
TOOL BIT, COUNTERBORING
ID
Range
2.141" thru 5.562"
(54.4 mm thru 141.3 mm)
2.141" thru 5.562"
(54.4 mm thru 141.3 mm)
2.546" thru 5.968"
(64.7 mm thru 151.6 mm)
2.546" thru 5.968"
(64.7 mm thru 151.6 mm)
3.562" thru 6.500"
(90.5 mm thru 165.1 mm)
3.562" thru 6.500"
(90.5 mm thru 165.1 mm)
14.5° (4:1) C'Bore
Pipe
Facing
(1/2" [12.7 mm])
or Tube
Tool Bit
Deep
Material
Tool Bit P/N
CS 99-2907 99-29-04
SS 99-2920 99-2917
CS 99-2908 99-2904
SS 99-2921 99-2917
CS 99-2909 99-2904
SS 99-2922 99-2917
P/N
30
92-0211 : Rev. 050224
Page 31
Model 206B BEVELMASTER™
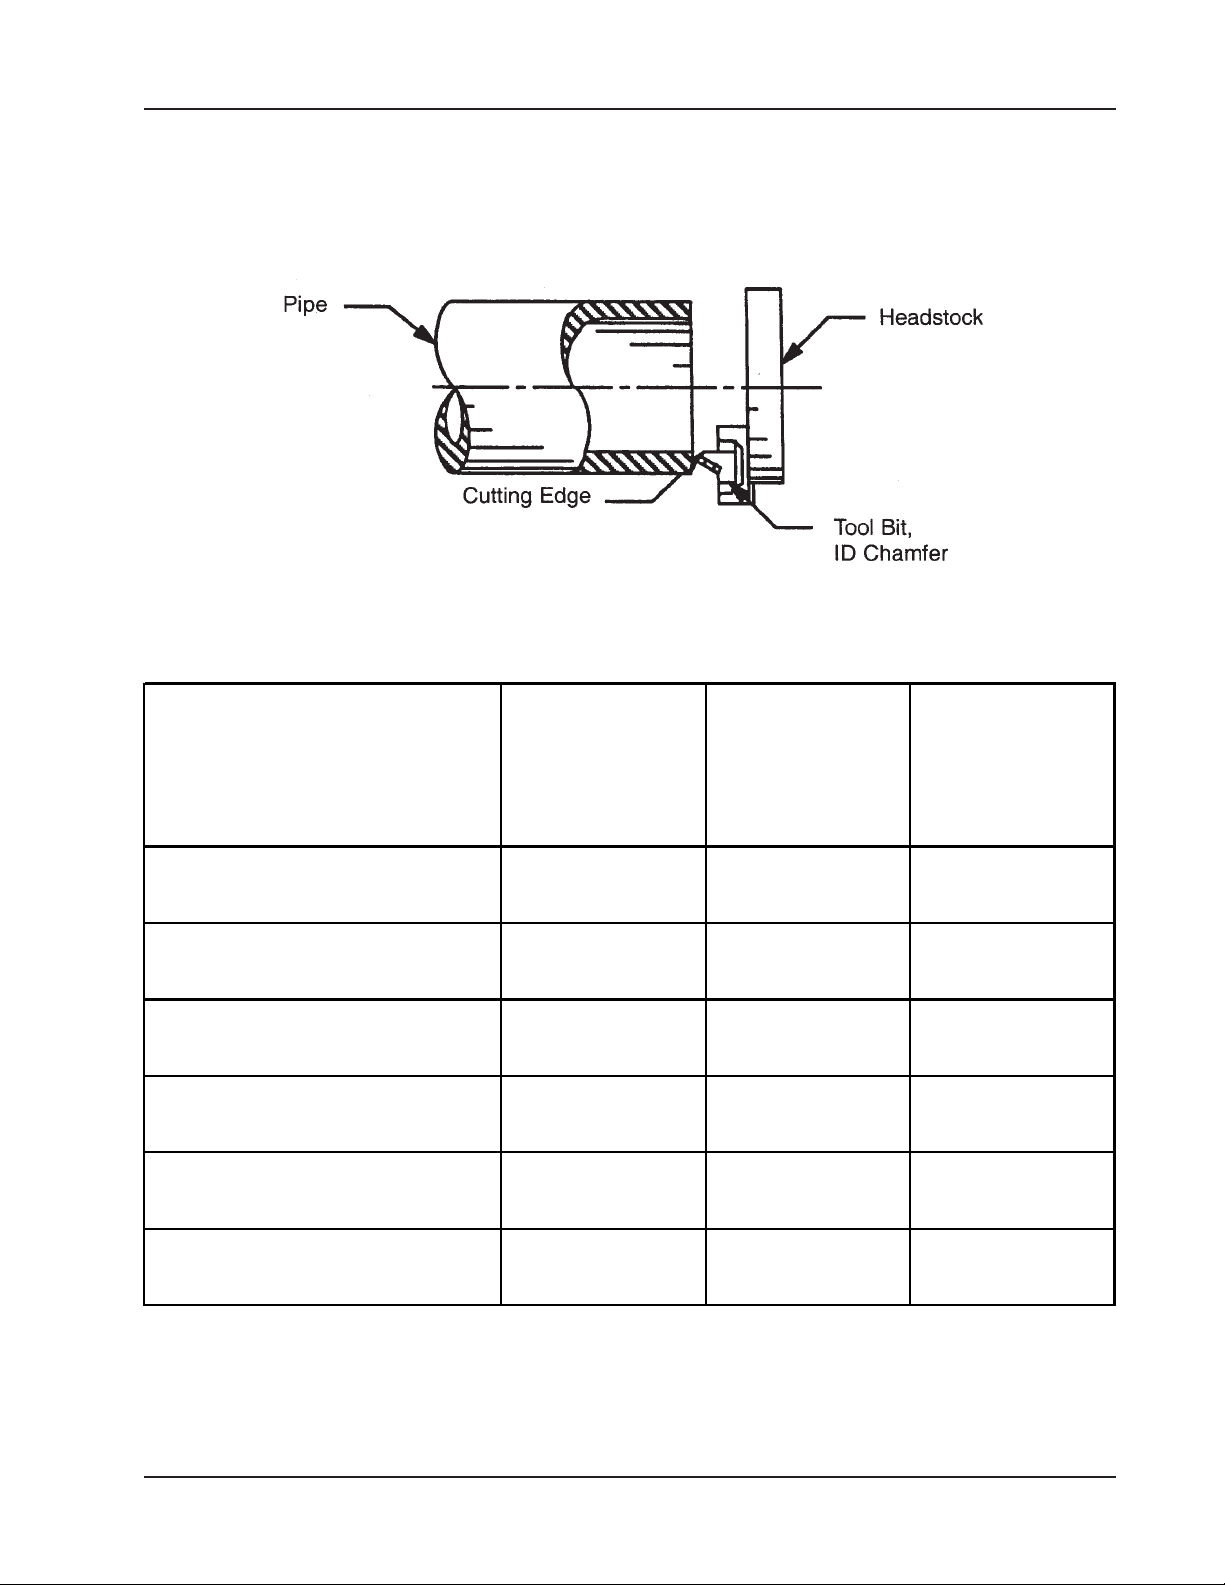
TOOL BIT, ID CHAMFER
ID
Range
2.000" thru 5.375"
(50.8 mm thru 136. 5 mm)
2.000" thru 5.375"
(50.8 mm thru 136. 5 mm)
2.812" thru 6.125"
(71.4 mm thru 155. 6 mm)
2.812" thru 6.125"
(71.4 mm thru 155. 6 mm)
3.546" thru 6.500"
(90.1 mm thru 165. 1 mm)
3.546" thru 6.500"
(90.1 mm thru 165. 1 mm)
Pipe
10° ID
Chamfer
or Tube
Tool Bit
Tool Bit
Material
P/N
CS 99-2910 99-2904
SS 99-2923 99-2917
CS 99-2911 99-2904
SS 99-2924 99-2917
CS 99-2912 99-2904
SS 99-2925 99-2917
Facing
P/N
92-0211 : Rev. 050224
31
Page 32
TRI TOOL INC.
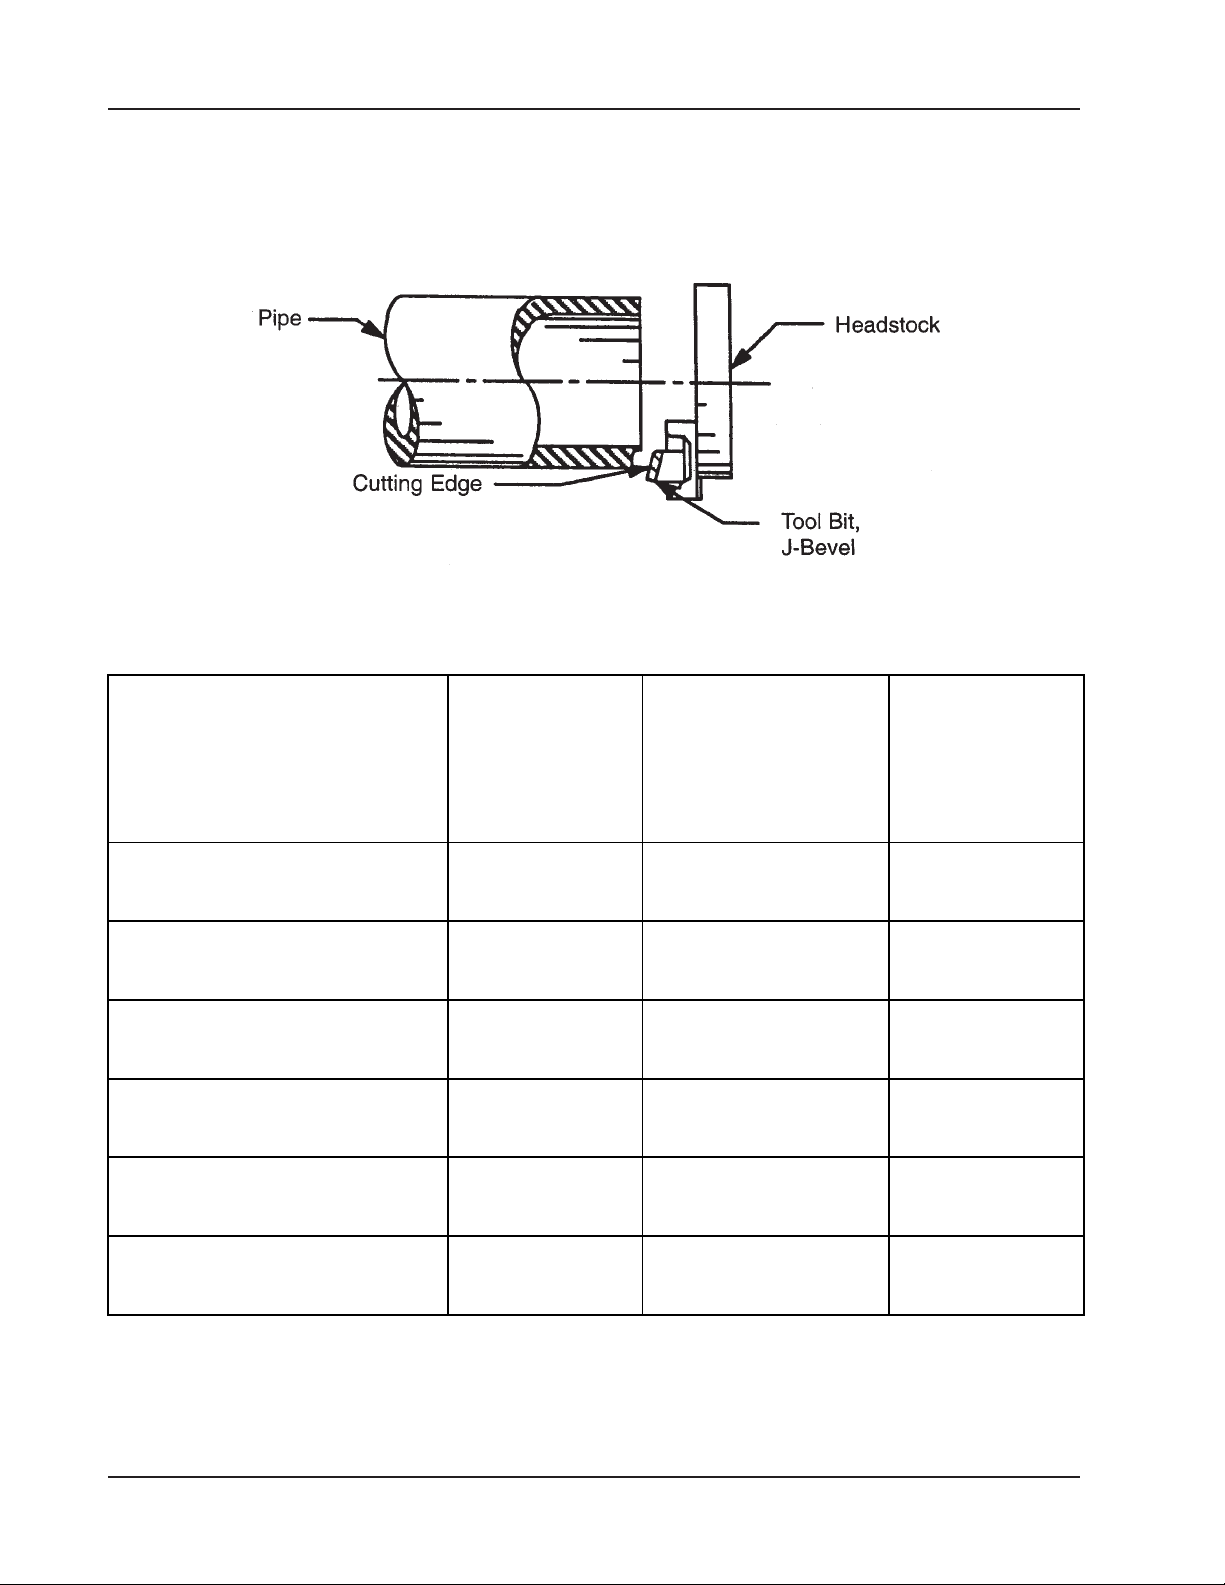
TOOL BIT, J-BEVEL
ID
Range
1.625" t hru 4. 750"
(41. 3 mm thru 1 20. 7 mm)
1.625" t hru 4. 750"
(41. 3 mm thru 1 20. 7 mm)
2.750" t hru 6. 000"
69.9 m m th r u 152.4 m m )
2.750" t hru 6. 000"
69.9 m m th r u 152.4 m m )
3.750" t hru 6. 625"
(95. 3 mm thru 1 68. 3 mm)
3.750" t hru 6. 625"
(95. 3 mm thru 1 68. 3 mm)
Pipe
25° J-B evel
or Tube
Tool Bit
Tool Bit
Material
P/N
CS 99-2915 99-2904
SS 99-2928 99-2917
CS 99-2916 99-2904
SS 99-2929 99-2917
CS 99-3349 99-2904
SS 99-3350 99-2917
Facing
P/N
32
92-0211 : Rev. 050224
Page 33
TROUBLE SHOOTING
Problem: The Tool Bit Chatters
The tool bit is loose or overextended.
The tool bit is damaged.
The tool holder is too loose in the slides.
The cutting speed is too fast.
The clamping pads are loose on the pipe or tube.
Cutting fluid is required.
The main bearing pre-load is loose.
Problem: There's Excessive Tool Bit Wear
Model 206B BEVELMASTER™
The pipe or tube material is too hard or abrasive.
The cutting speed is too fast.
Cutting fluid is required.
A dull Tool Bit is causing surface hardening conditions (Stainless pipe or
tubing).
There is scale or other foreign matter on the pipe or tube, which is dulling the
tool bit at the start of the cut.
The tool bit is incorrect for the material being cut.
Problem: The Surface Finish is Rough
The tool bit is dull, chipped, etc.
Metal build-up on the cutting edge of the tool bit is creating a false cutting
edge.
Cutting fluid is required.
Problem: The Tool Holder is Not Feeding
The feed pin is broken or out of position.
The feed sprocket shear pin is broken.
The feed screw is stripped.
The feed nut is stripped.
The slide rails are too tight.
92-0211 : Rev. 050224
33
Page 34
TRI TOOL INC.
Problem: There's a Loss of Air Power
The air supply pressure is too low.
The air filter is plugged.
The air line size is insufficient.
The air line is too long.
Problem: There's a Loss of Hydraulic Power
The hydraulic supply pressure is too low.
The hydraulic filter is plugged.
The hydraulic line size is insufficient.
The hydraulic line is too long.
Problem: The Tool Bit Will Not Reach the Work
Incorrect tool blocks are installed for the size of the pipe or tube being worked
on.
Incorrect tool bit is installed.
Problem: The Hydraulic Motor Will Not Start
The hydraulic power supply is shut off.
The hydraulic motor is damaged and will not run free.
34
92-0211 : Rev. 050224
Page 35
Model 206B BEVELMASTER™
ACCESSORIES
The following accessories are recommended for use with the Model 206B and are
available from TRI TOOL INC.
1. Portable Air Caddy (P/N 75-0115)
2. Elbow Mandrel Kit (P/N 05-1257)
2.51” ID to 6.12” ID
(63.8 mm ID to 155.4 mm ID)
3. Elbow Mandrel Assembly (P/N 06-0296)
1.63” ID to 2.56” ID
(41.4 mm ID to 65.0 mm ID)
4. Pointer kit, Elbow Mandrel (P/N 05-0153)
5. Sleeve Mandrel Kit (P/N 05-1286)
2” – 6” pipe
6. Flange Facer Kit (P/N 05-0131)
1.75” DIA to 14.00” DIA
(44.5 mm DIA to 355.6 mm DIA)
7. Miter Mandrel Kit (P/N 05-0177)
8. Dial Indicator Kit (P/N 05-0180)
9. ID Tracking Module Kit (P/N 05-0183)
NOTE:
A (FRL) is required to protect the warranty on all TRI TOOL INC. air driven
tools.
92-0211 : Rev. 050224
35
Page 36
TRI TOOL INC.
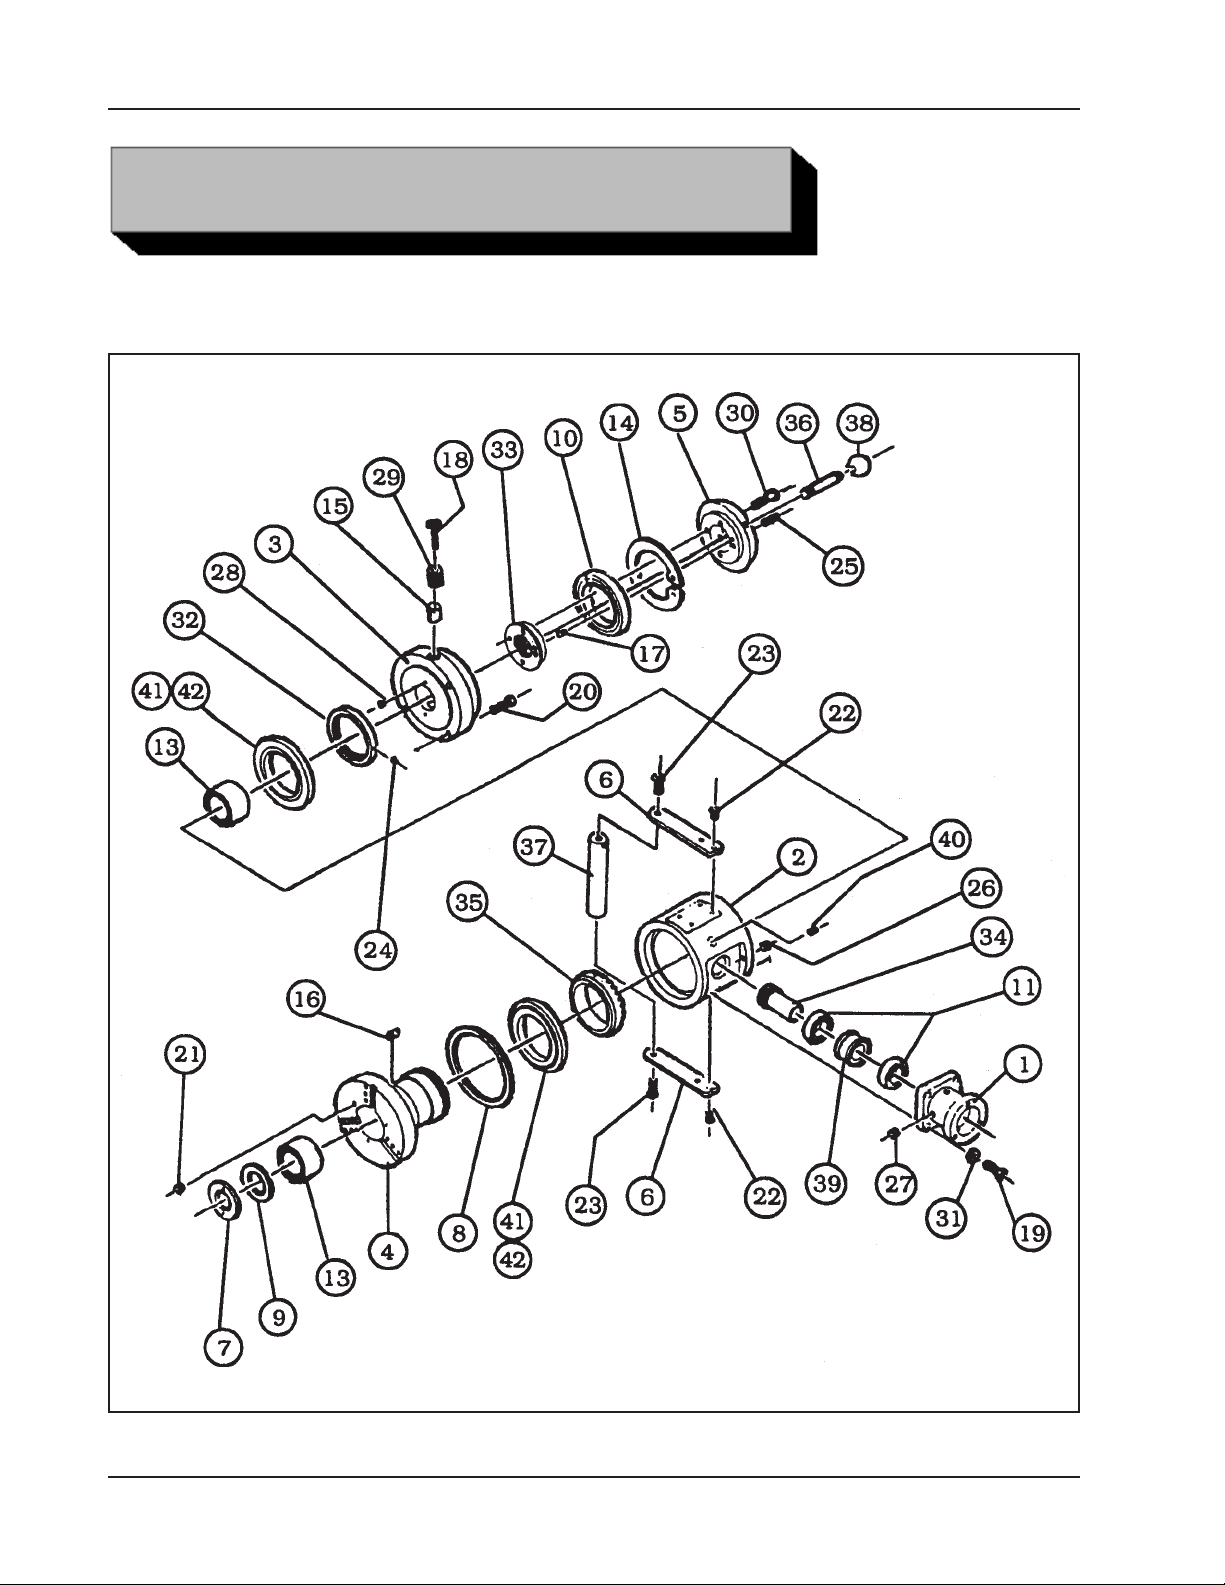
ILLUSTRATED PARTS BREAKDOWN
MODEL 206B BEVELMASTER™
36
92-0211 : Rev. 050224
Page 37
Model 206B BEVELMASTER™
Parts List, Model 206B BEVELMASTER™
Item Part
No. No. Description Qty
1. 19-0409 HOUSING, DRIVE 1
2. 19-0410 HOUSING, MAIN 1
3. 19-0411 HOUSING, FEED 1
4. 20-0358 SHAFT, MAIN 1
5. 24-0726 PLATE, FEED 1
6. 24-0727 PLATE, HANDLE 2
7. 24-0831 PLATE, SEAL 1
8. 28-0057 SEAL, FELT 17"
(44 cm)
9. 28-0172 SEAL, SHAFT 1
10. 29-0002 BEARING, BALL 1
11. 29-0065 BEARING, BALL 2
12. —-
13. 29-0218 BEARING, ROLLER 2
92-0211 : Rev. 050224
37
Page 38
TRI TOOL INC.
Parts List, Model 206B BEVELMASTER™ Continued
Item Part
No. No. Description Qty
14. 30-0300 RING, RETAINING, INTERNAL 1
15. 31-0086 KEY, BRONZE, 45° 2
16. 31-0087 KEY 1
17. 32-0304 PIN, LOCK 1
18. 33-0031 SCREW, CAP, #10-24 X 7/8" 2
19. 33-0056 SCREW, CAP, 5/16-18 X 1" 4
20. 33-0058 SCREW, CAP, 5/16-18 X 1 1/2" 4
21. 33-0284 SCREW, BUTTON HEAD, 1/4-20 X 3/8" 3
22. 33-0285 SCREW, BUTTON HEAD, 1/4-20 X 1/2" 4
23. 33-0300 SCREW, BUTTON HEAD, 3/8-16 X 1" 2
24. 33-0488 SCREW, SET, #10-24 X 1/4", CUP PT 2
25. 33-0507 SCREW, SET, 1/4-20 X 1", CUP PT 1
26. 33-0515 SCREW, SET, 5/16-18 X 7/16", CUP PT 1
27. 33-0526 SCREW, SET, 3/8-16 X 5/16, CUP PT 4
28. 33-0954 SCREW, SET, #10-24, 1/4", HDOG 2
29. 33-1524 SCREW, SET, ADJUST 2
30. 33-1526 SCREW, BUTTON HEAD, 5/16-18 X 1 1/2" 4
31. 34-0027 WASHER, FLAT 4
32. 35-0267 NUT, LOCK 1
33. 35-0269 NUT, FEED 1
34. 39-0331 GEAR, PINION 1
35. 39-0468 GEAR, BEVEL 1
36. 41-0076 HANDLE, FEED 4
37. 41-0077 HANDLE 1
38. 42-0017 KNOB 4
39. 46-0134 SLEEVE 1
40. 54-0375 FITTING, GREASE 1
41. 29-0216 BEARING, TAPER, CONE 2
42. 29-0215 BEARING, TAPER, CUP 2
NOT SHOWN
05-1256 SHIPPING KIT 1
36-0005 WRENCH, L, 1/8" HEX 1
36-0007 WRENCH, L, 5/32" HEX 1
38
92-0211 : Rev. 050224
Page 39
Model 206B BEVELMASTER™
Parts List, Model 206B BEVELMASTER™ Continued
Item Part
No. No. Description Qty
NOT SHOWN Continued
36-0008 WRENCH, L, 3/16" HEX 1
36-0010 WRENCH, L, 1/4" HEX 1
36-0012 WRENCH, L, 3/8" HEX 1
36-0020 WRENCH, T, 5/32" HEX 1
36-0146 WRENCH, COMBINATION, 13/16" 1
86-0089 CARRYING CASE, 206B 1
92-0211 : Rev. 050224
39
Page 40
TRI TOOL INC.
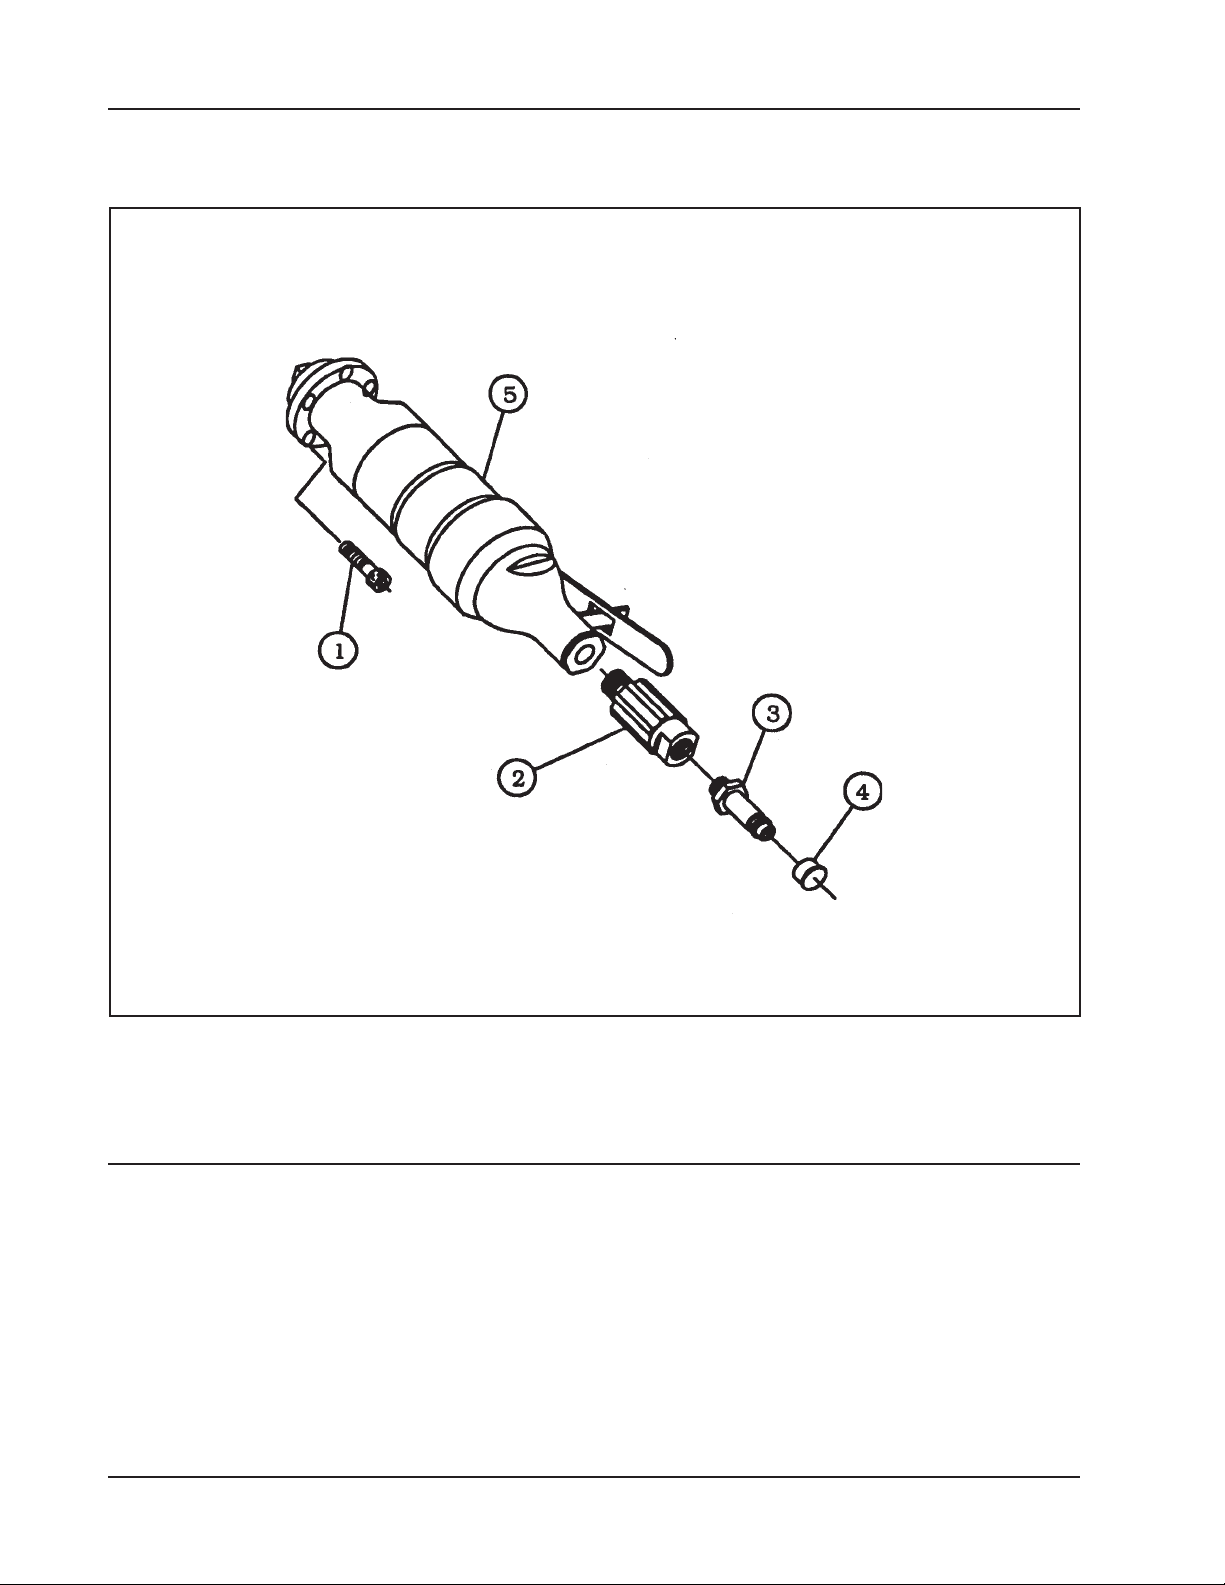
MOTOR ASSEMBLY, AIR (P/N 57-0168)
Parts List, Motor Assembly, Air (P/N 57-0168)
Item Part
No. No. Description Qty
1. 33-0056 SCREW, CAP, 5/16-18 X 1" 3
2. 53-0046 VALVE, FLOW CONTROL 1
3. 54-0126 COUPLING, QD 1
4. 54-0201 CAP, PLASTIC 1
5. 57-0161 MOTOR, AIR 1
40
92-0211 : Rev. 050224
Page 41
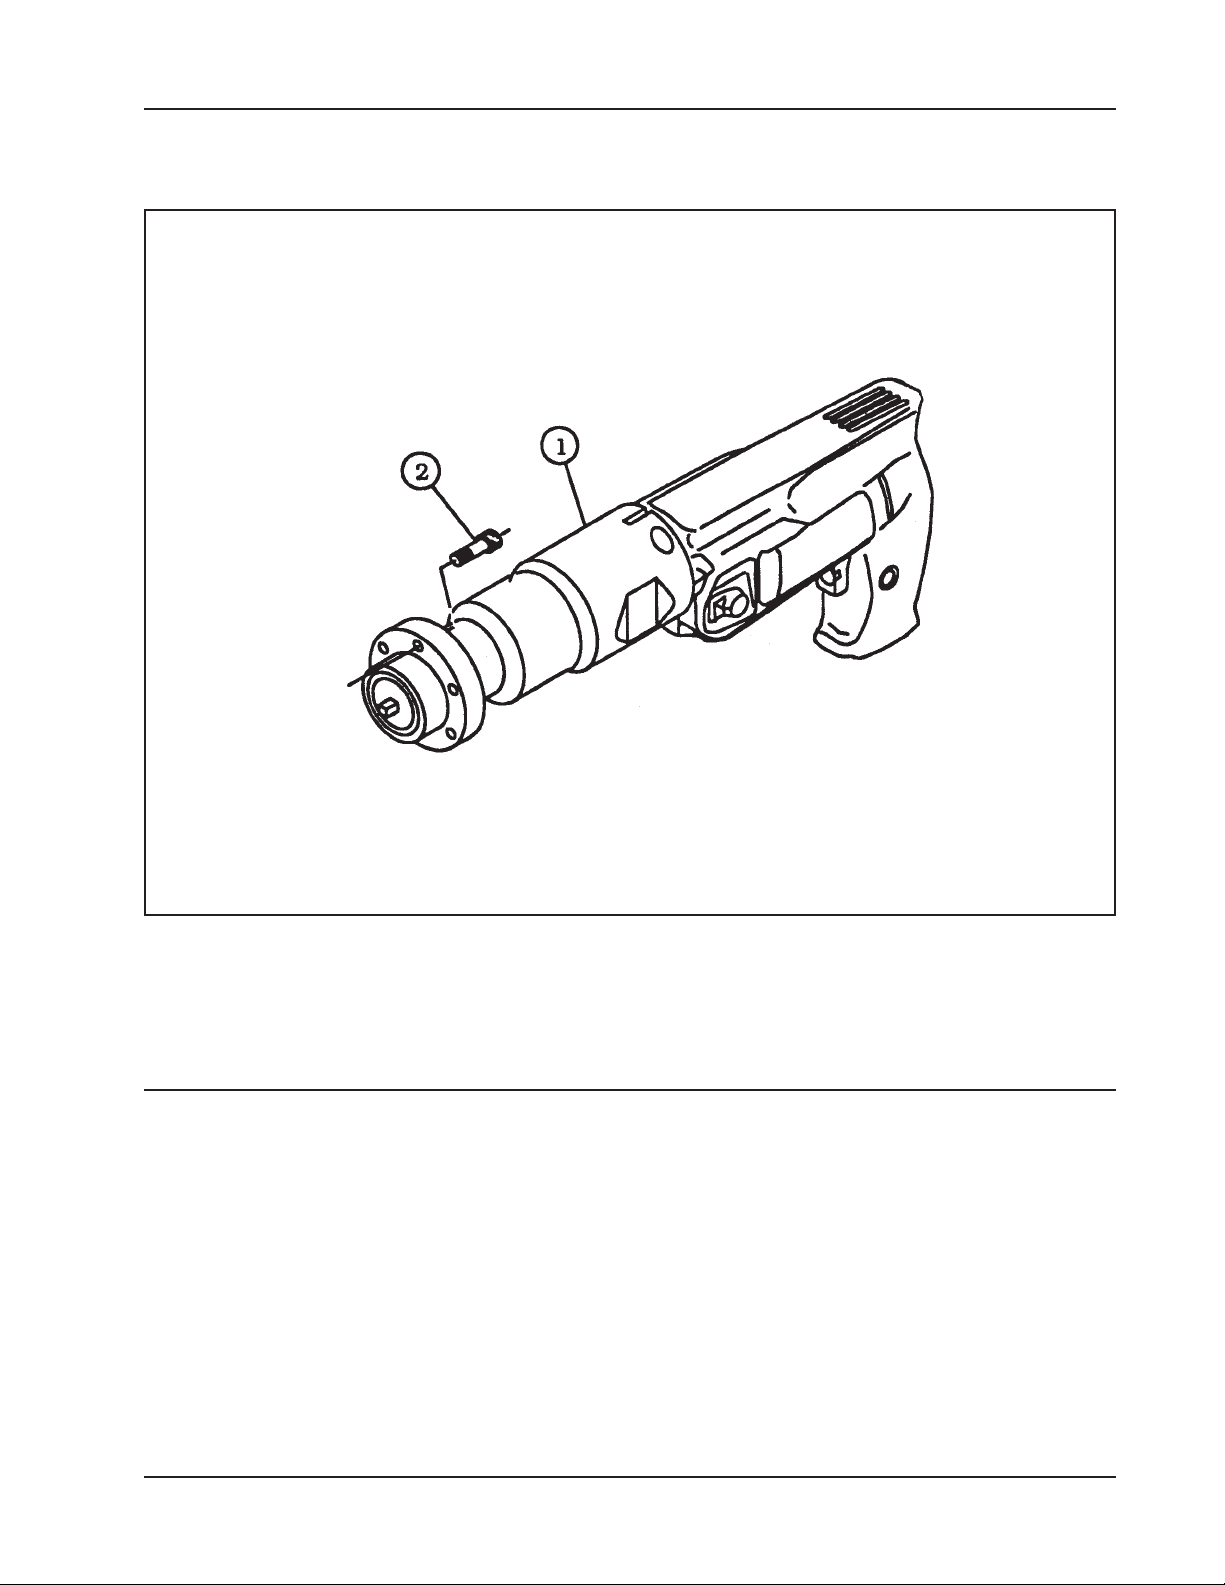
Model 206B BEVELMASTER™
MOTOR ASSEMBLY, ELECTRIC
Parts List, Motor Assembly, Electric
Item Part
No. No. Description Qty
110V AC, 60 Hz
1. 58-0045 MOTOR ASSEMBL Y, ELECTRIC 1
2. 33-0056 SCREW, CAP, 5/16-18 X 1" 3
220V AC, 50 Hz
1. 58-0047 MOTOR ASSEMBL Y, ELECTRIC 1
2. 33-0056 SCREW, CAP, 5/16-18 X 1" 3
92-0211 : Rev. 050224
41
Page 42
TRI TOOL INC.
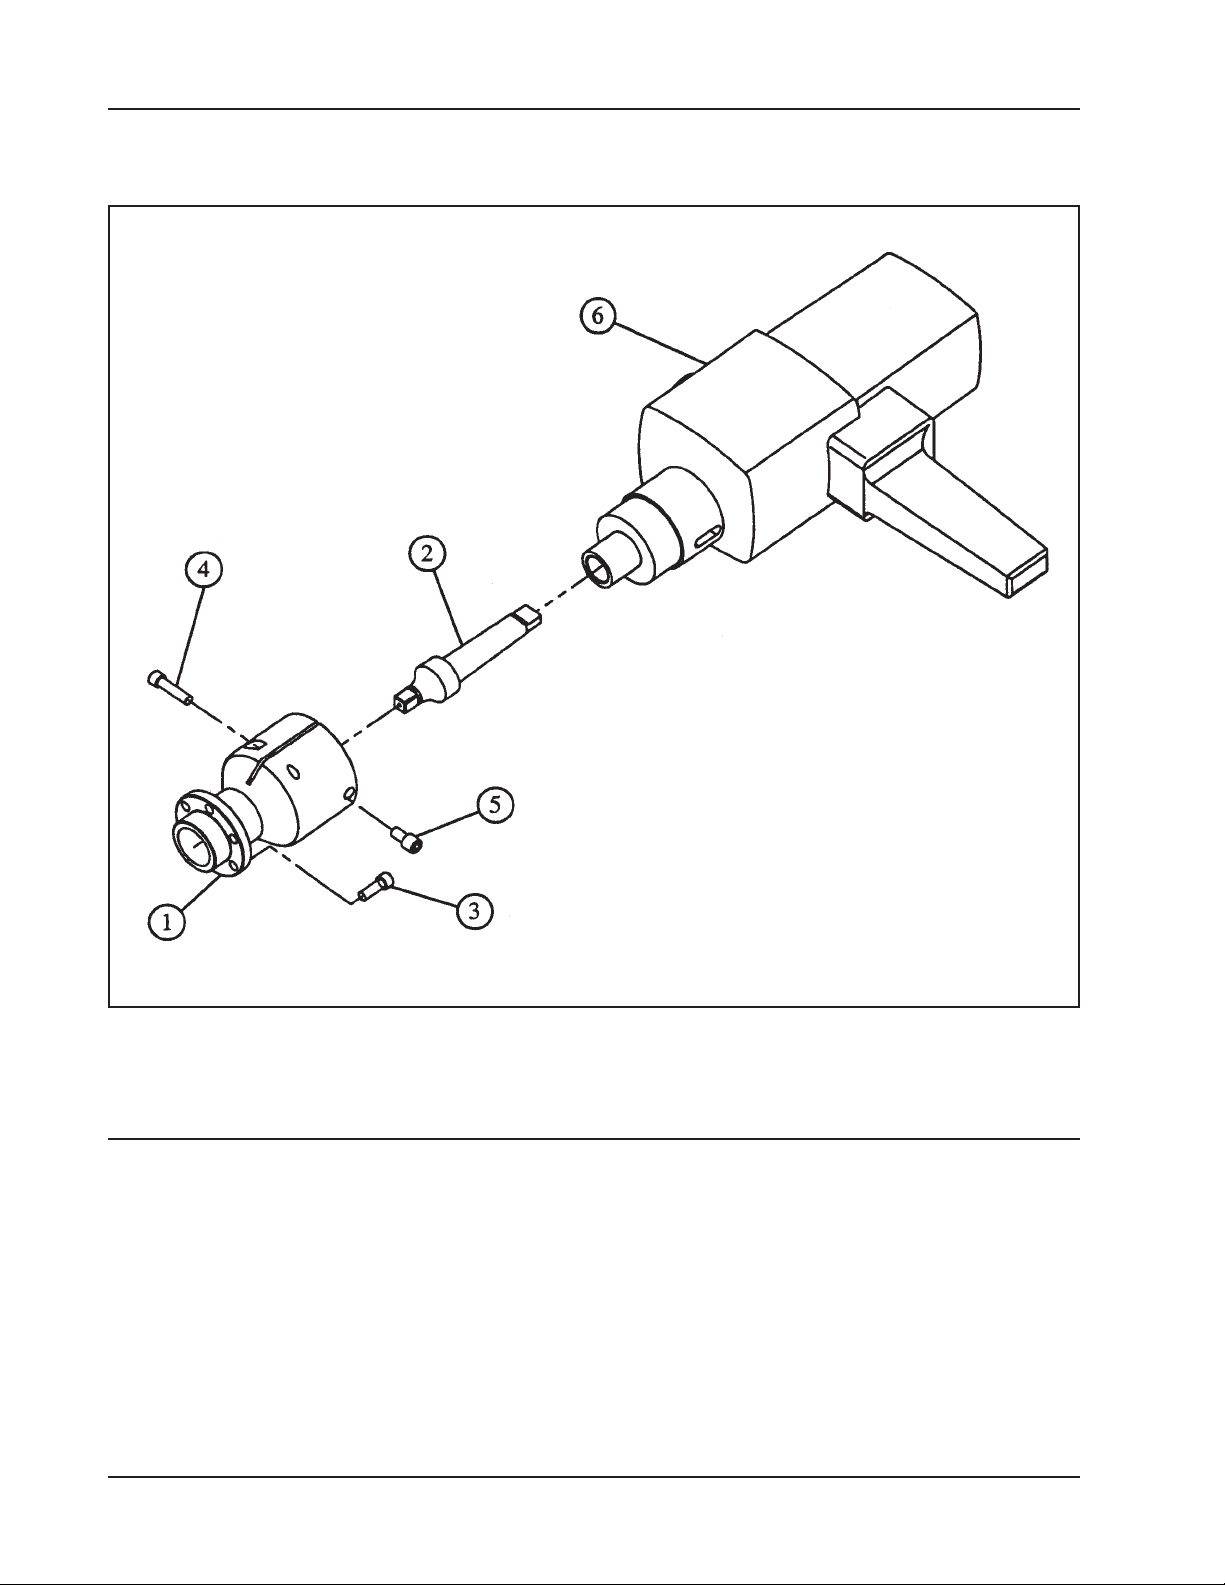
MOTOR ASSEMBLY, ELECTRIC DRIVE, 115V HD (P/N 58-0167)
Parts List, Motor Assembly, Electric Drive, 115V HD (P/N 58-0167)
Item Part
No. No. Description Qty
1. 27-0826 ADAPTER, DRIVE 1
2. 30-3143 1/2" SQUARE DRIVE 1
3. 33-0055 SCREW, CAP, 5/16-18 X 7/8" LG. 3
4. 33-0057 SCREW, CAP, 5/16-18 X 1 1/4" LG. 1
5. 33-1874 SCREW, ANTI-ROTATION 2
6. 58-0192 MOTOR, ELECTRIC, 115V, MODIFIED 1
42
92-0211 : Rev. 050224
Page 43
Model 206B BEVELMASTER™
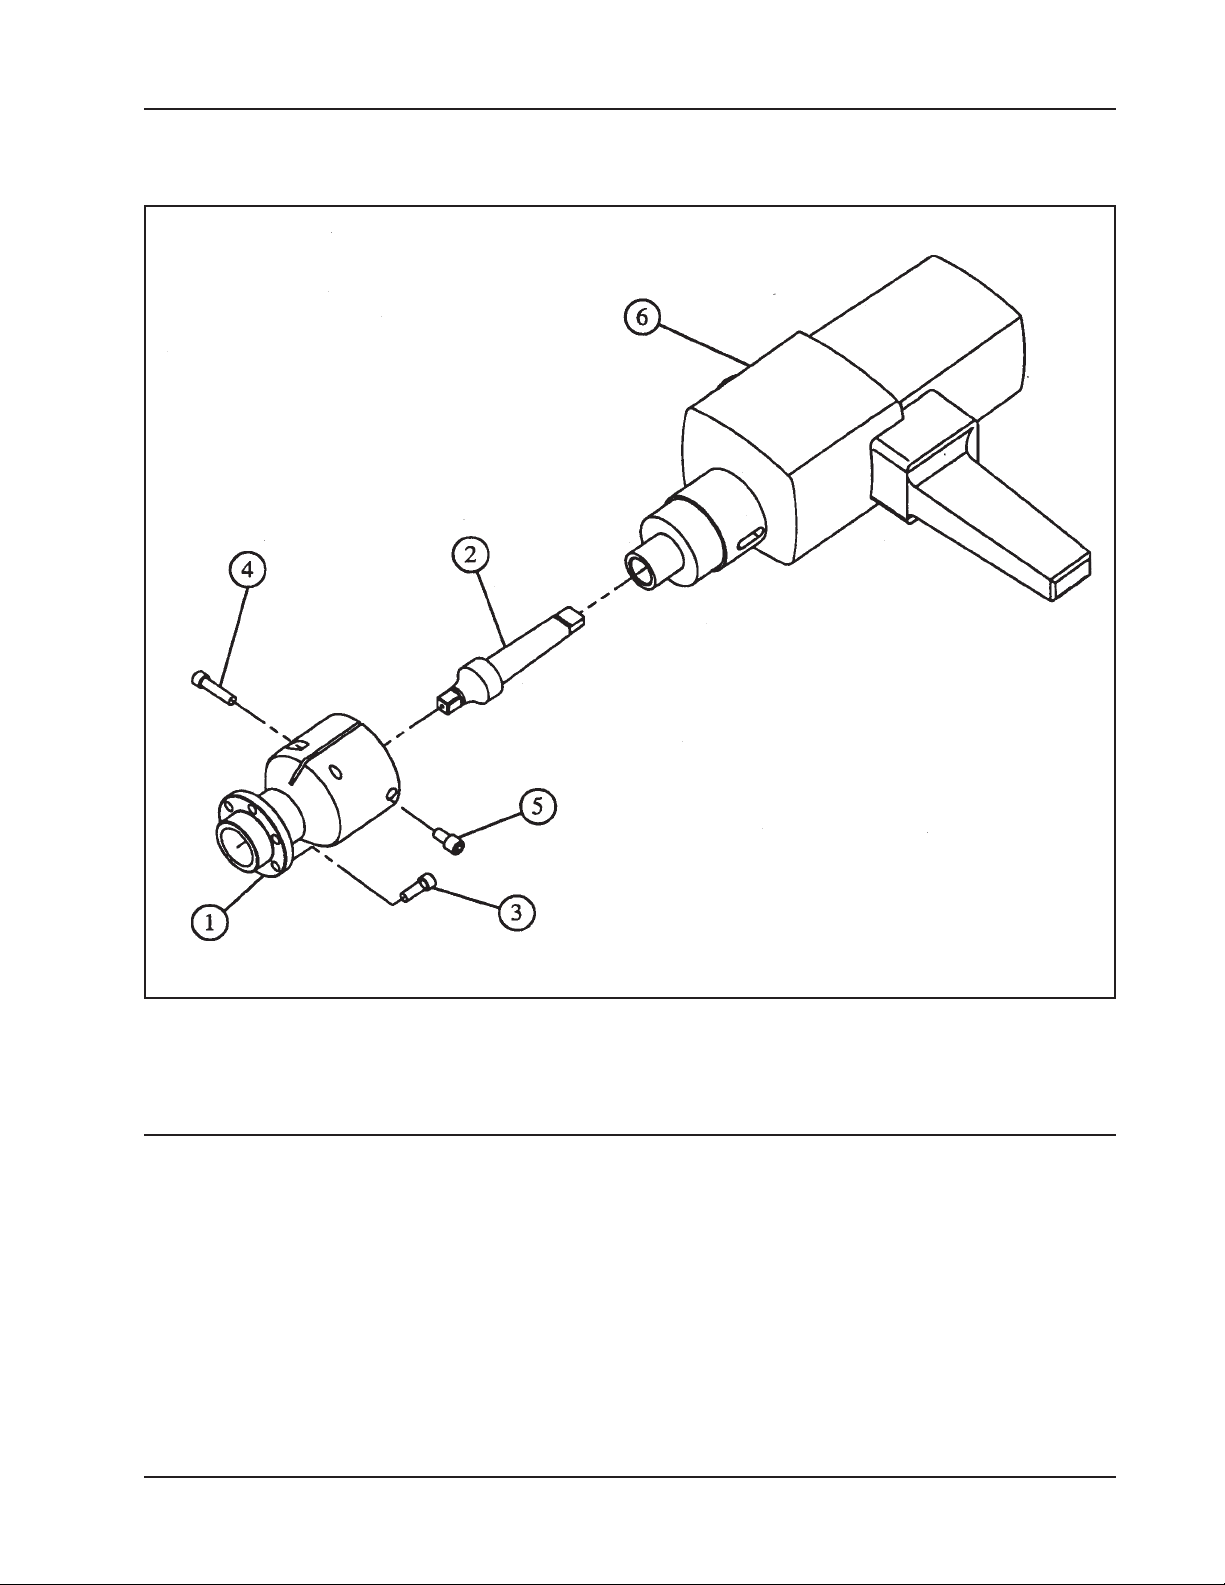
MOTOR ASSEMBLY, ELECTRIC DRIVE, 230V HD (P/N 58-0174)
Parts List, Motor Assembly, Electric Drive, 230V HD (P/N 58-0174)
Item Part
No. No. Description Qty
1. 27-0826 ADAPTER, DRIVE 1
2. 30-3143 1/2" SQUARE DRIVE 1
3. 33-0055 SCREW, CAP, 5/16-18 7/8" LG. 3
4. 33-0057 SCREW, CAP, 5/16-18 X 1 1/4" LG. 1
5. 33-1874 SCREW, ANTI-ROTATION 2
6. 58-0173 MOTOR, ELECTRIC, 230V, MODIFIED 1
92-0211 : Rev. 050224
43
Page 44
TRI TOOL INC.
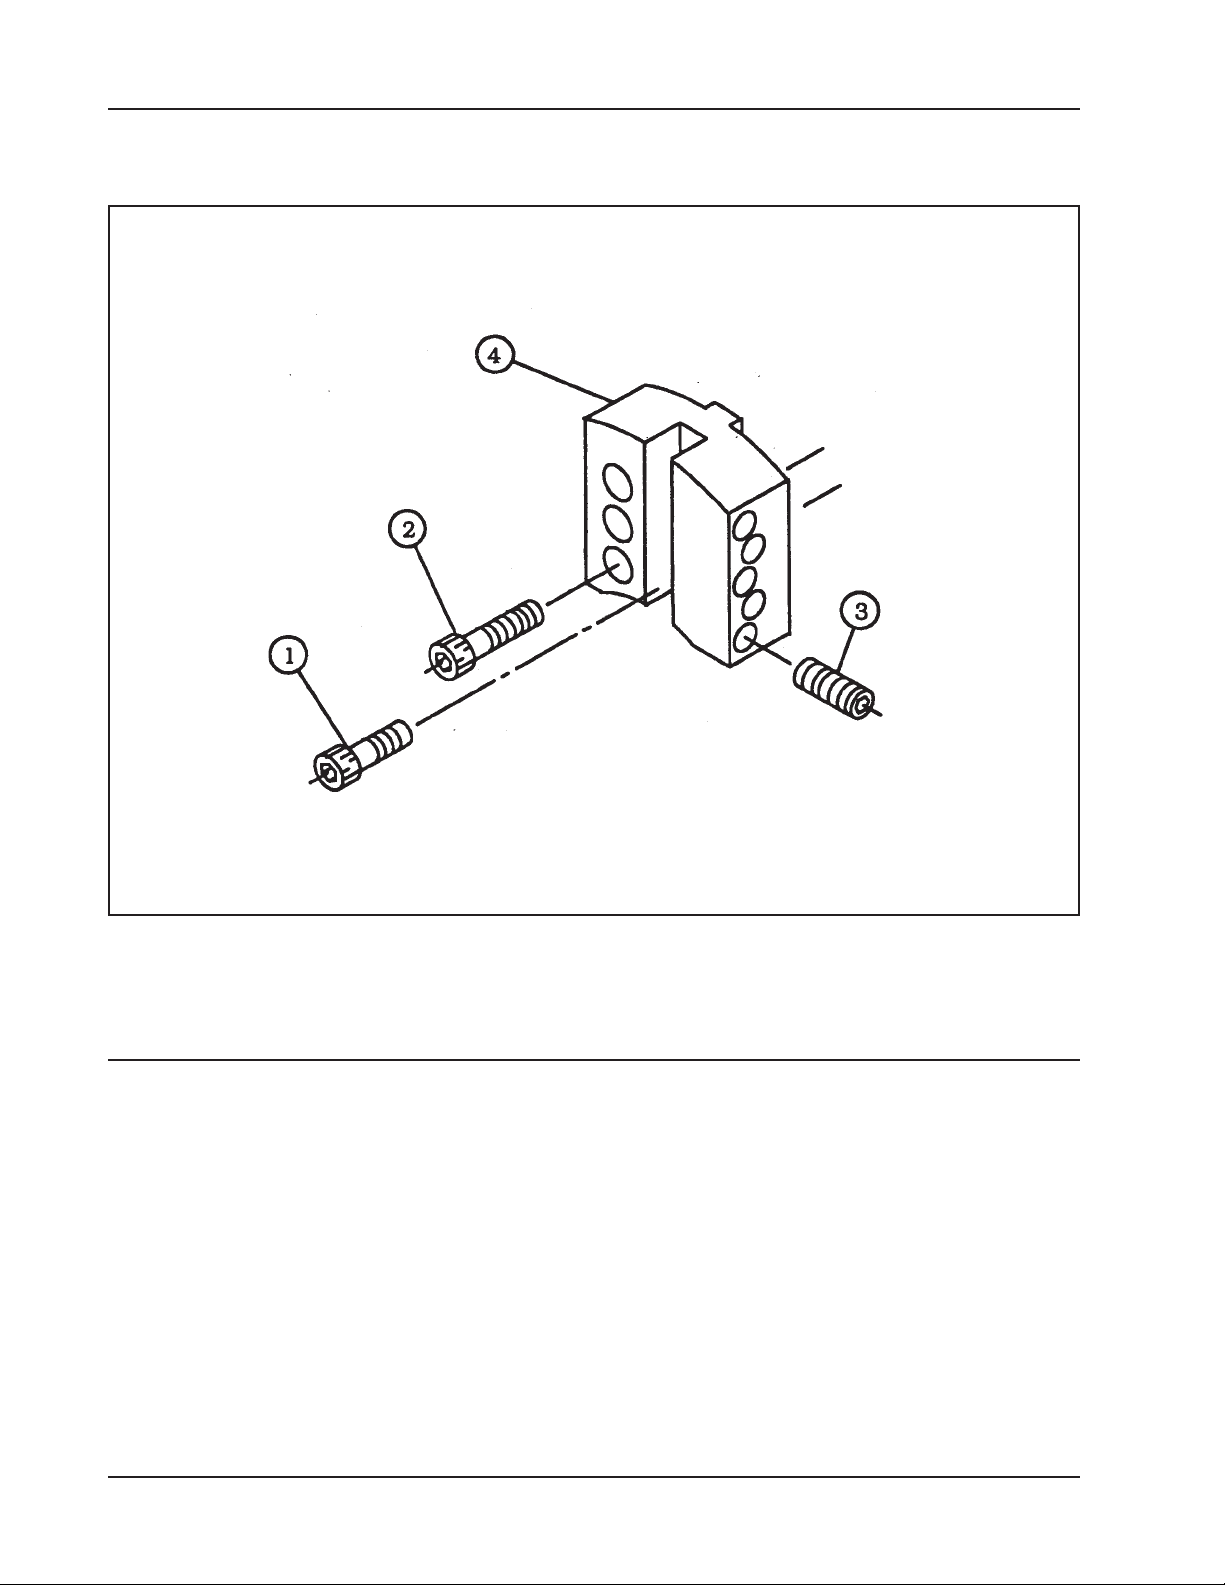
TOOL HOLDER (P/N 49-0089)
Parts List, Tool Holder (P/N 49-0089)
Item Part
No. No. Description Qty
1. 33-0039 SCREW, CAP, 1/4-20 X 5/8" 3
2. 33-0042 SCREW, CAP, 1/4-20 X 1" 3
3. 33-0518 SCREW, SET, 5/16-18 X 3/4", CUP PT 5
4. 49-0087 HOLDER, TOOL 1
44
92-0211 : Rev. 050224
Page 45
Model 206B BEVELMASTER™
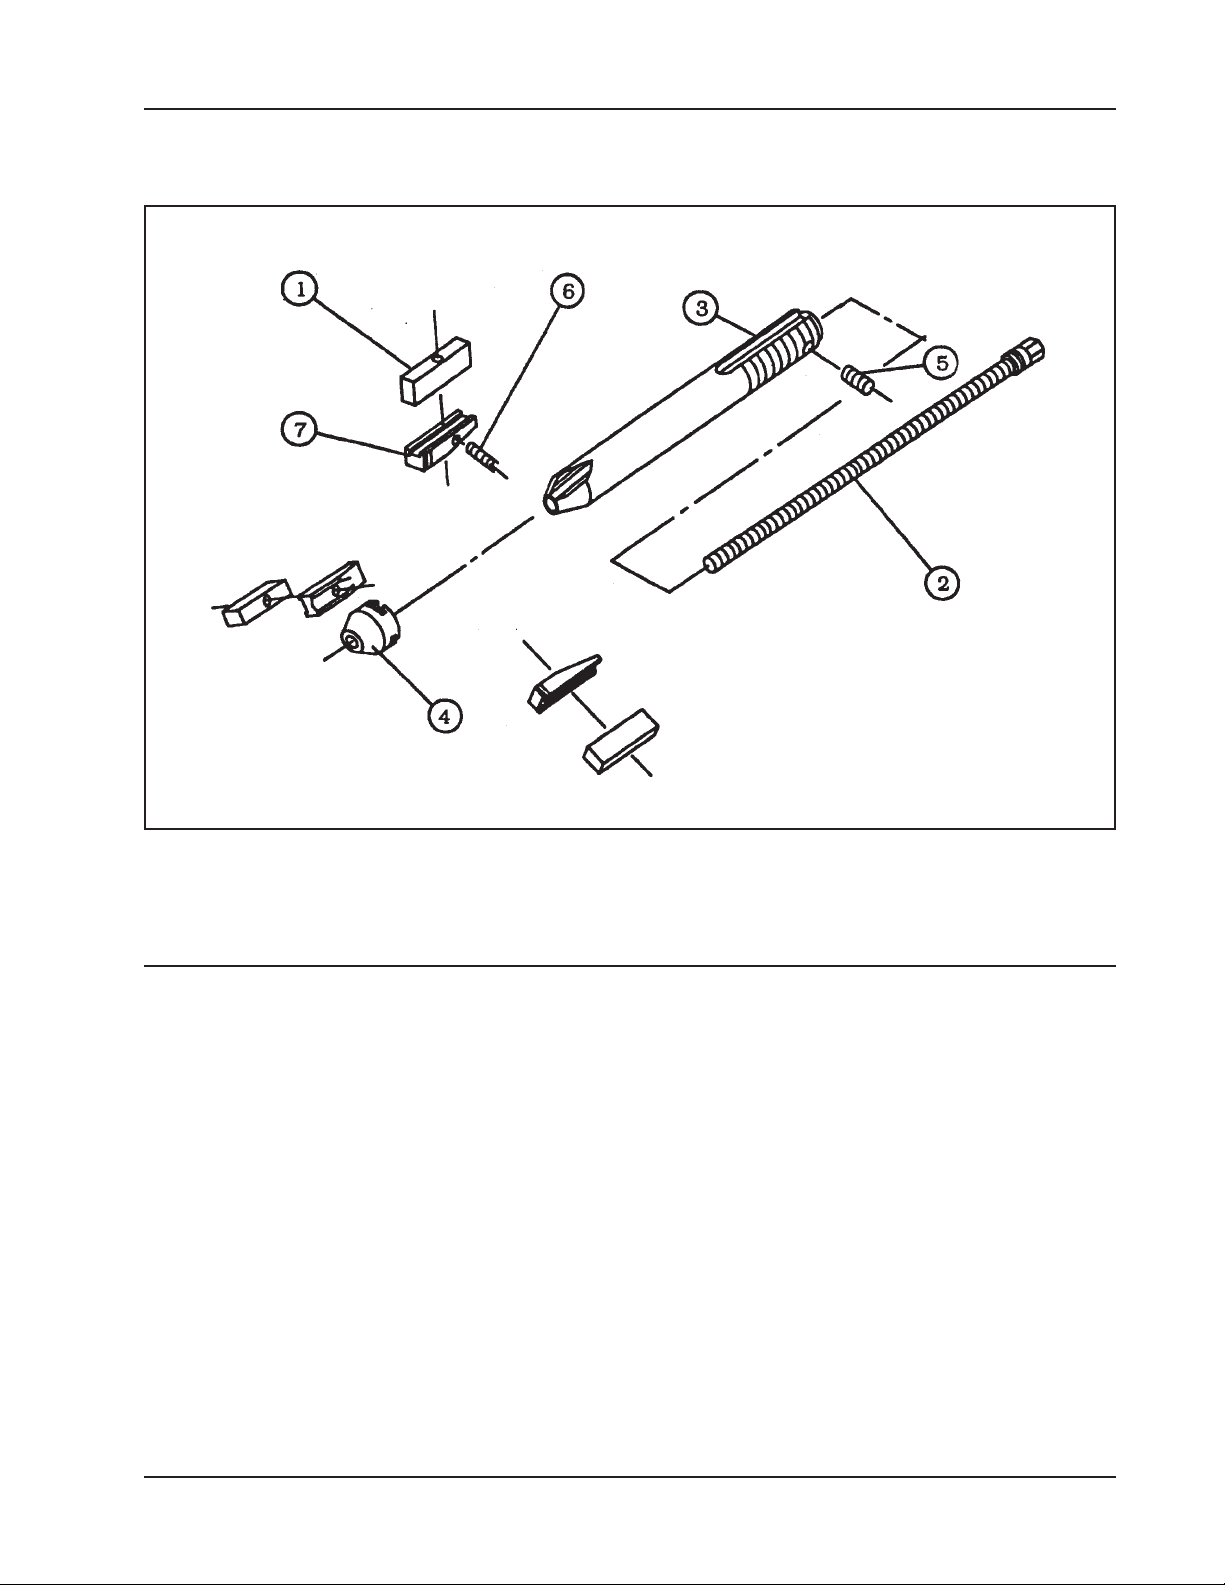
MANDREL ASSEMBLY (P/N 06-0292)
Parts List, Mandrel Assembly (P/N 06-0292)
Item Part
No. No. Description Qty
1. 08-0162 BLOCK ASSEMBL Y, JAW , .340" 3
08-0163 BLOCK ASSEMBL Y, JAW , .580" 3
08-0164 BLOCK ASSEMBL Y, JAW , .820" 3
08-0165 BLOCK ASSEMBLY, JAW, 1.060" 3
2. 11-0057 ROD ASSEMBLY , DRAW 1
3. 13-0301 MANDREL 1
4. 24-0722 PLATE, BUTT, SMALL 1
24-0723 PLATE, BUTT, LARGE 1
5. 33-1527 SCREW, SET, 1/4-20 X 1/4", H DOG 2
6. 40-0001 SPRING, EXTENSION 1
40-0037 SPRING, EXTENSION 1
7. 48-0474 BLOCK, RAMP, STANDARD 3
48-0475 BLOCK, RAMP, EXTENDED 3
92-0211 : Rev. 050224
45
 Loading...