

Page 1
JAA80051-R.3741.A
M
サービス
計画課
INC
作成承認印 配布許可印
AF-S DX Nikkor
16-85mm f/3.5-5.6G ED VR
JAA80051
REPAIR MANUAL
Printed in Japan February 2008
Copyrightc2008 by Nikon Corporation.
All Rights Reserved.
無断転載を禁ず
!!
Page 2
JAA80051-R.3741.A
INC
※ Before Disassembly / Reassembly / Adjustment
This lens will require optical lens alignment after assembly, in case the 4th lens-group unit is removed.
At repair service facilities, therefore, where this alignment work can not be performed, do NOT remove the
4th lens-group unit.
This lens also has the VR (vibration-reduction) unit mounted in order to correct camera shake.
To keep the accuracy of this function for stabilizing the image, in case VR unit or the main PCB is replaced,
be sure to make the VR adjustment by using the VR lens adjustment equipment (J15380).
Except for disassembling the above components, the VR adjustment is NOT necessary, but check VR
operations by attaching this lens to the camera.
At repair service facilities where the "VR lens adjustment equipment" is not prepared, do NOT disassemble
NOR repair the products of the above cases.
Caution:
When disassembling/(re)assembling, be sure to use the conductive mat (J5033) and wrist strap
(J5033-5) for static protection of electrical parts.
When disassembling, make sure to memorize the processing state of wires, screws to be fi xed and
their types, etc.
Because prototypes are used for "1. Disassembly" and "2. Assembly/Adjustment", they may differ
from the actual products in forms, etc.
Because pictures are processed by a special method, they may differ from the actual ones in texture.
Points to notice for Lead-free solder products
・Lead-free solder is used for this product.
・For soldering work, the special solder and soldering iron are required.
・Do NOT mix up lead-free solder with traditional solder.
・Use the special soldering iron respectively for lead-free solder and lead solder.
They cannot be used in common.
- D1・AF-S DX 16-85/3.5-5.6G VR -
Page 3
JAA80051-R.3741.A
INC
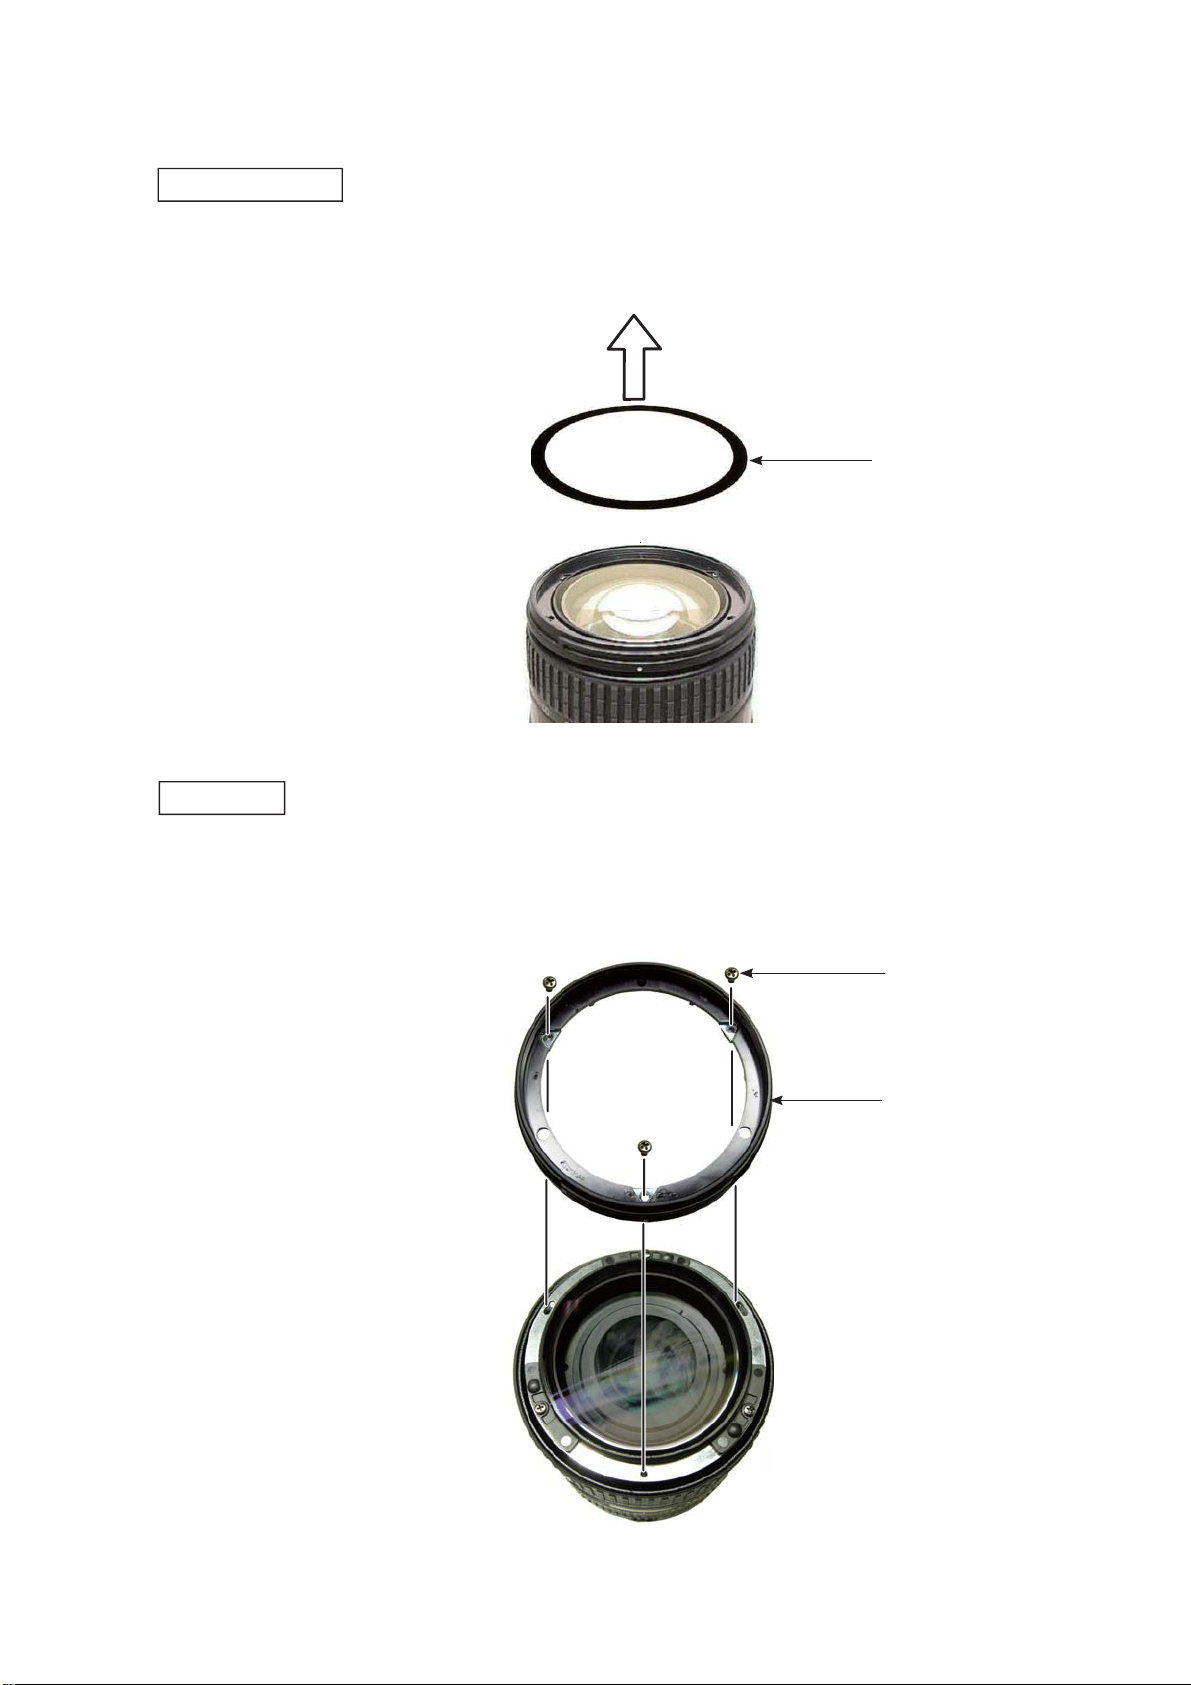
1.Disassembly
Protection sheet
Peel off the protection sheet (#60) by inserting tweezers from the outside into the cutout of attaching face as
・
below.
#60
Filter ring
Take out the three screws (#119) and remove the fi lter ring (#35).
・
#119×3
#35
- D2・AF-S DX 16-85/3.5-5.6G VR -
Page 4
JAA80051-R.3741.A
INC
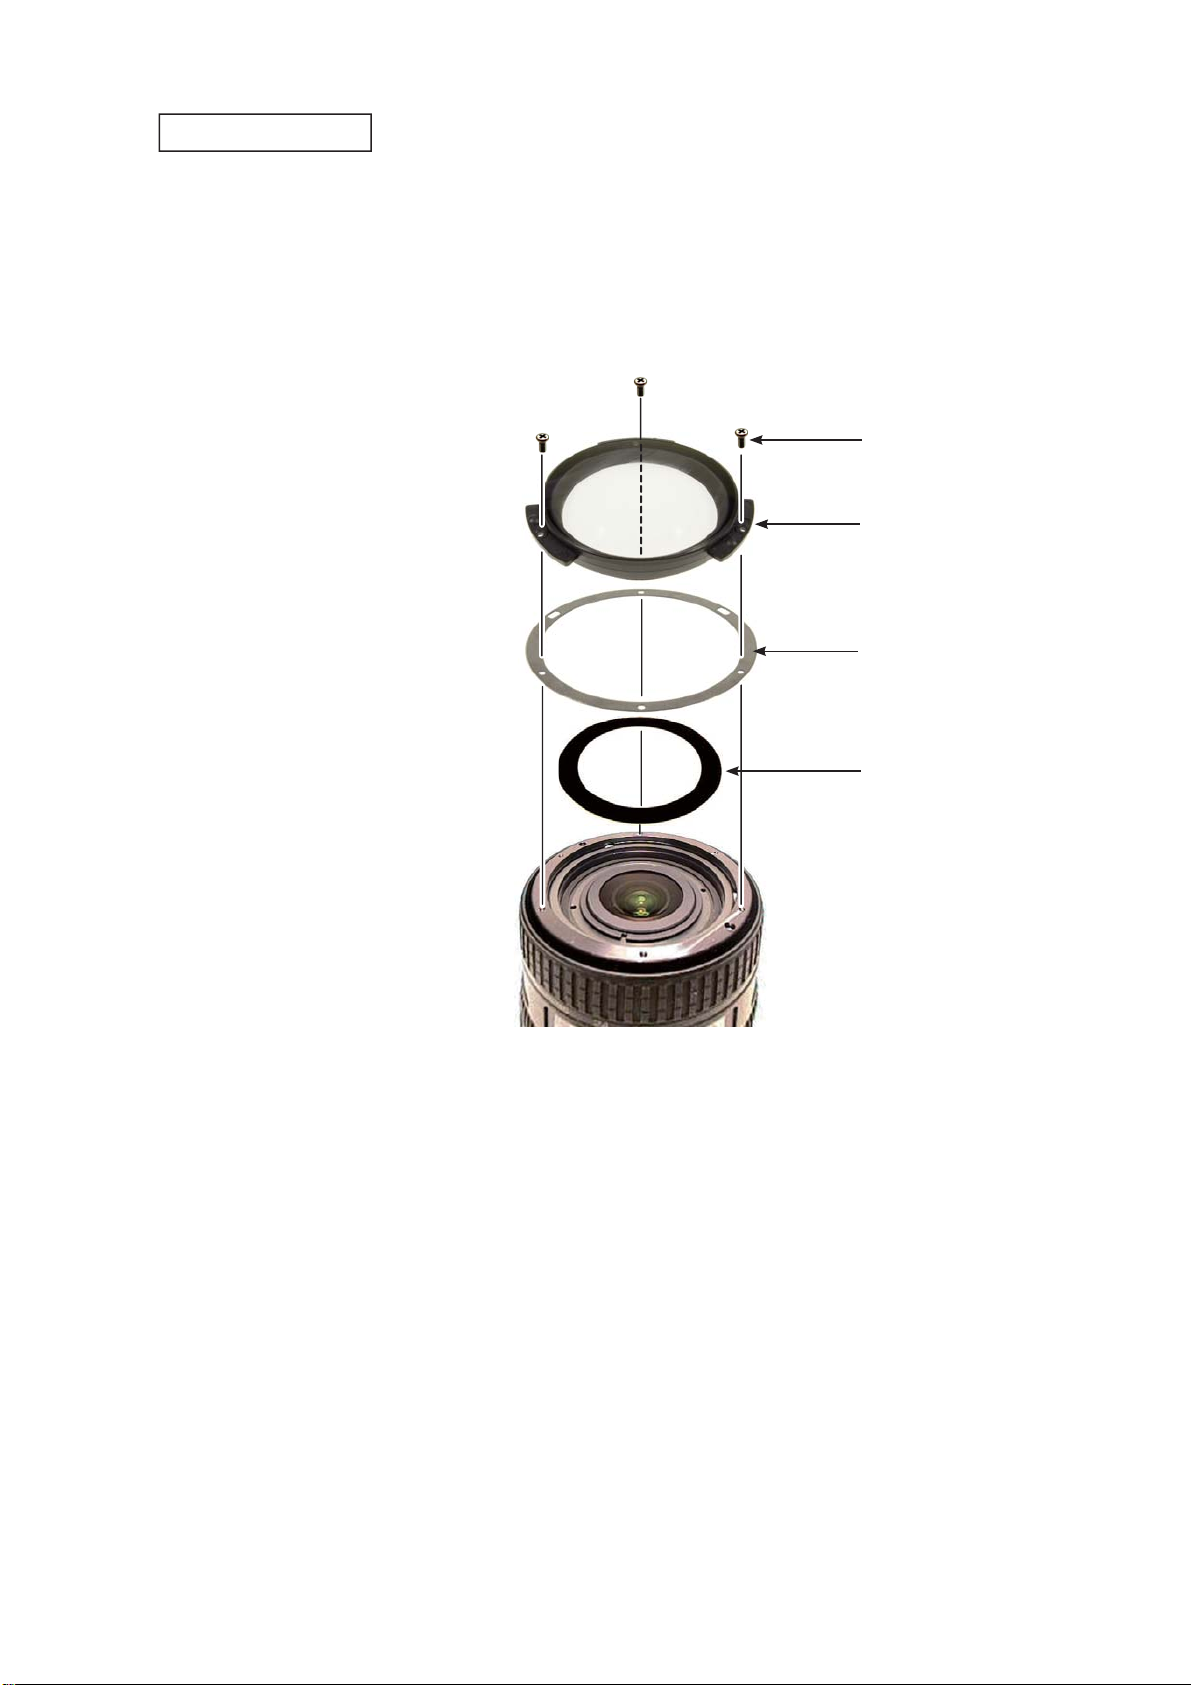
1st lens group unit
Set the zoom ring to WIDE.
・
Take out the three screws (#120) and remove the 1st lens-G unit (B2041) and washer (#133).
・
Peel off the sheet (#62).
・
#120×3
B2041
#133
#62
- D3・AF-S DX 16-85/3.5-5.6G VR -
Page 5
JAA80051-R.3741.A
INC
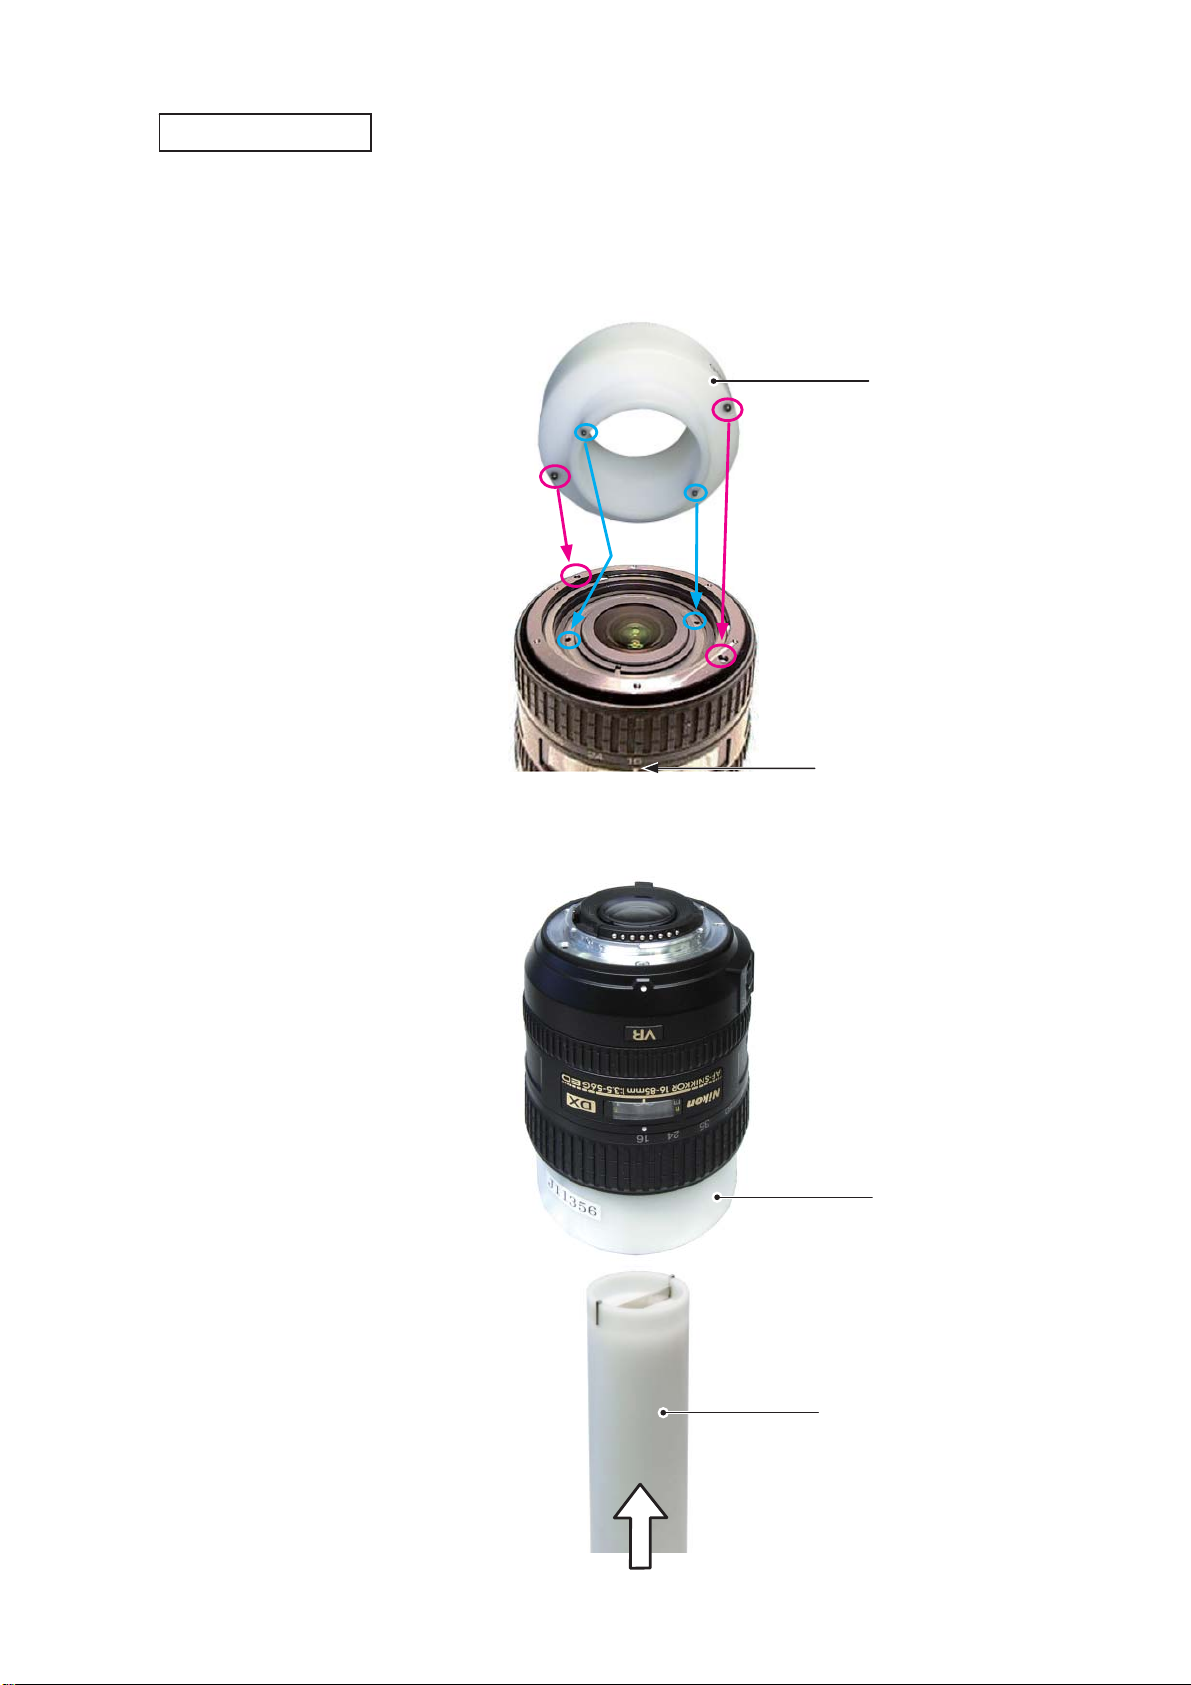
2nd lens group unit
Set the zoom ring to WIDE-end.
・
Set the focus index (#49) to "∞" position.
・
Mount the fi xing tool for 2nd lens-G (★J11356) by fi tting its protrusions in the holes of the 1st lens-G cam
・
ring (#38) and the 2nd lens-G cam ring (#25).
J11356
★
Index
Insert the wrench for the 2nd lens-G (★J11358) into the 2nd lens-group unit (B2043).
・
★
J11356
- D4・AF-S DX 16-85/3.5-5.6G VR -
J11358
★
Page 6
JAA80051-R.3741.A
INC
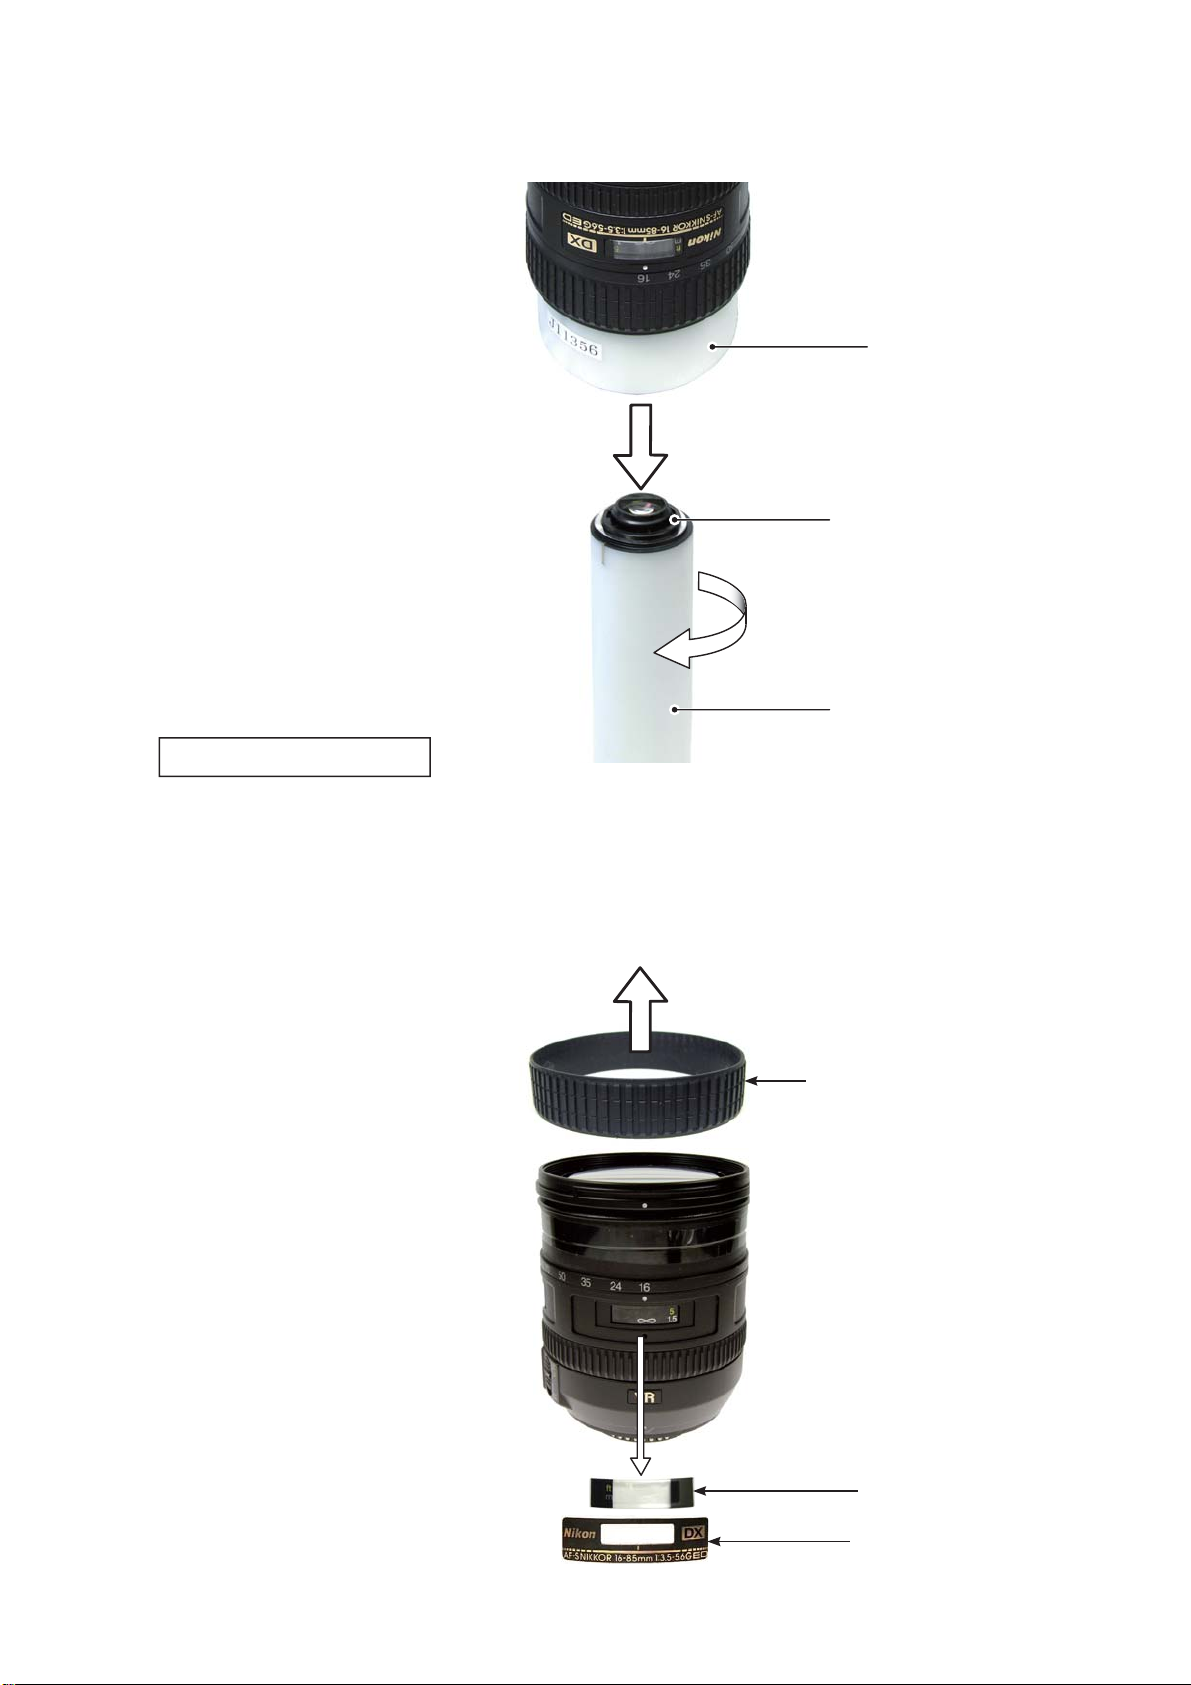
Turn the wrench for 2nd lens-G (★J11358) counterclockwise, and remove the 2nd lens-group unit (B2043).
・
J11356
★
B2043
J11358
★
Name plate/Focus window
Remove the rubber ring (#37).
・
Remove the name plate (#75) and focus window (#76).
・
Caution: Remove the name plate (#75) and focus window (#76) ONLY when they must be replaced because of
defects, etc.
#37
#76
#75
- D5・AF-S DX 16-85/3.5-5.6G VR -
Page 7
JAA80051-R.3741.A
INC
VR name plate / Serial No.label
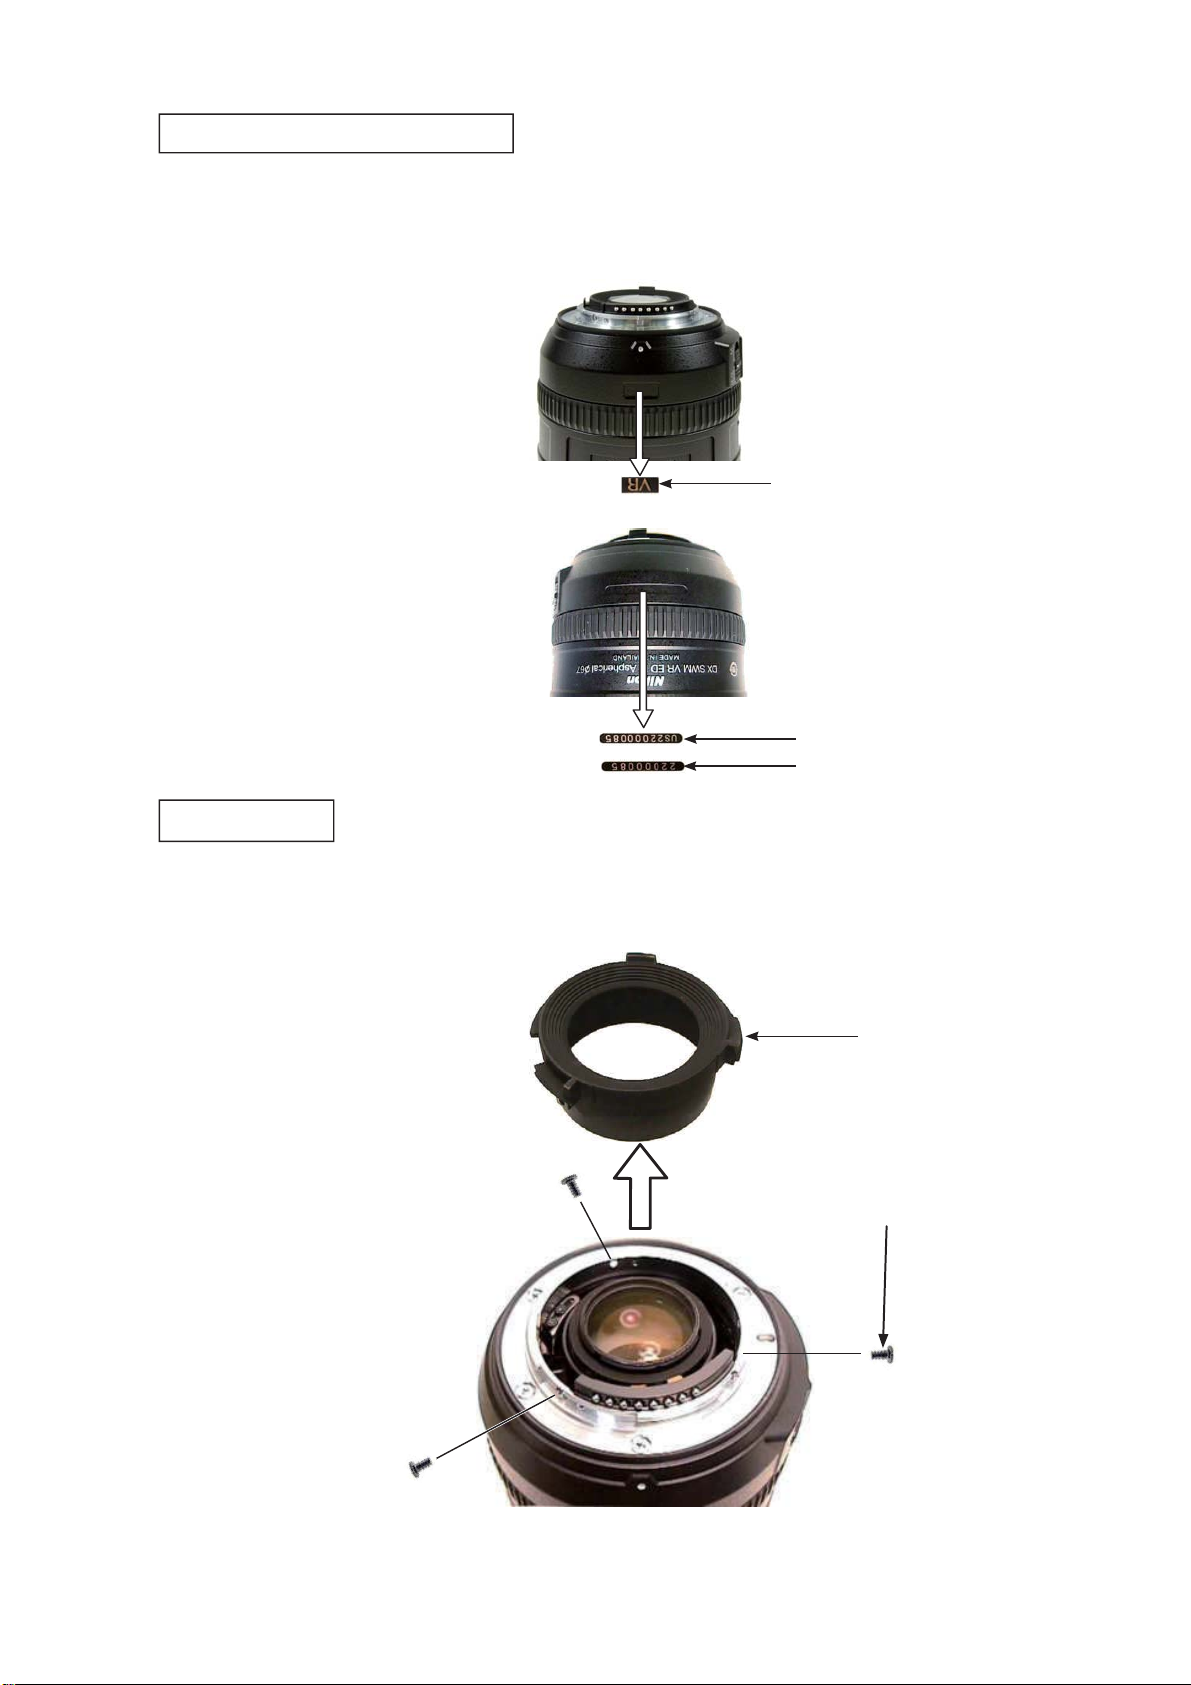
Remove VR name plate (#69) and serial number label (#168 or #169).
・
Caution: Remove VR name plate (#69) and serial number label (#168 or #169) ONLY when they must be
replaced because of defects, etc.
#69
Rear cover ring
Take out the three screws (#118) and remove the rear cover ring (#39).
・
#169
#168
#39
#118×3
- D6・AF-S DX 16-85/3.5-5.6G VR -
Page 8
JAA80051-R.3741.A
INC
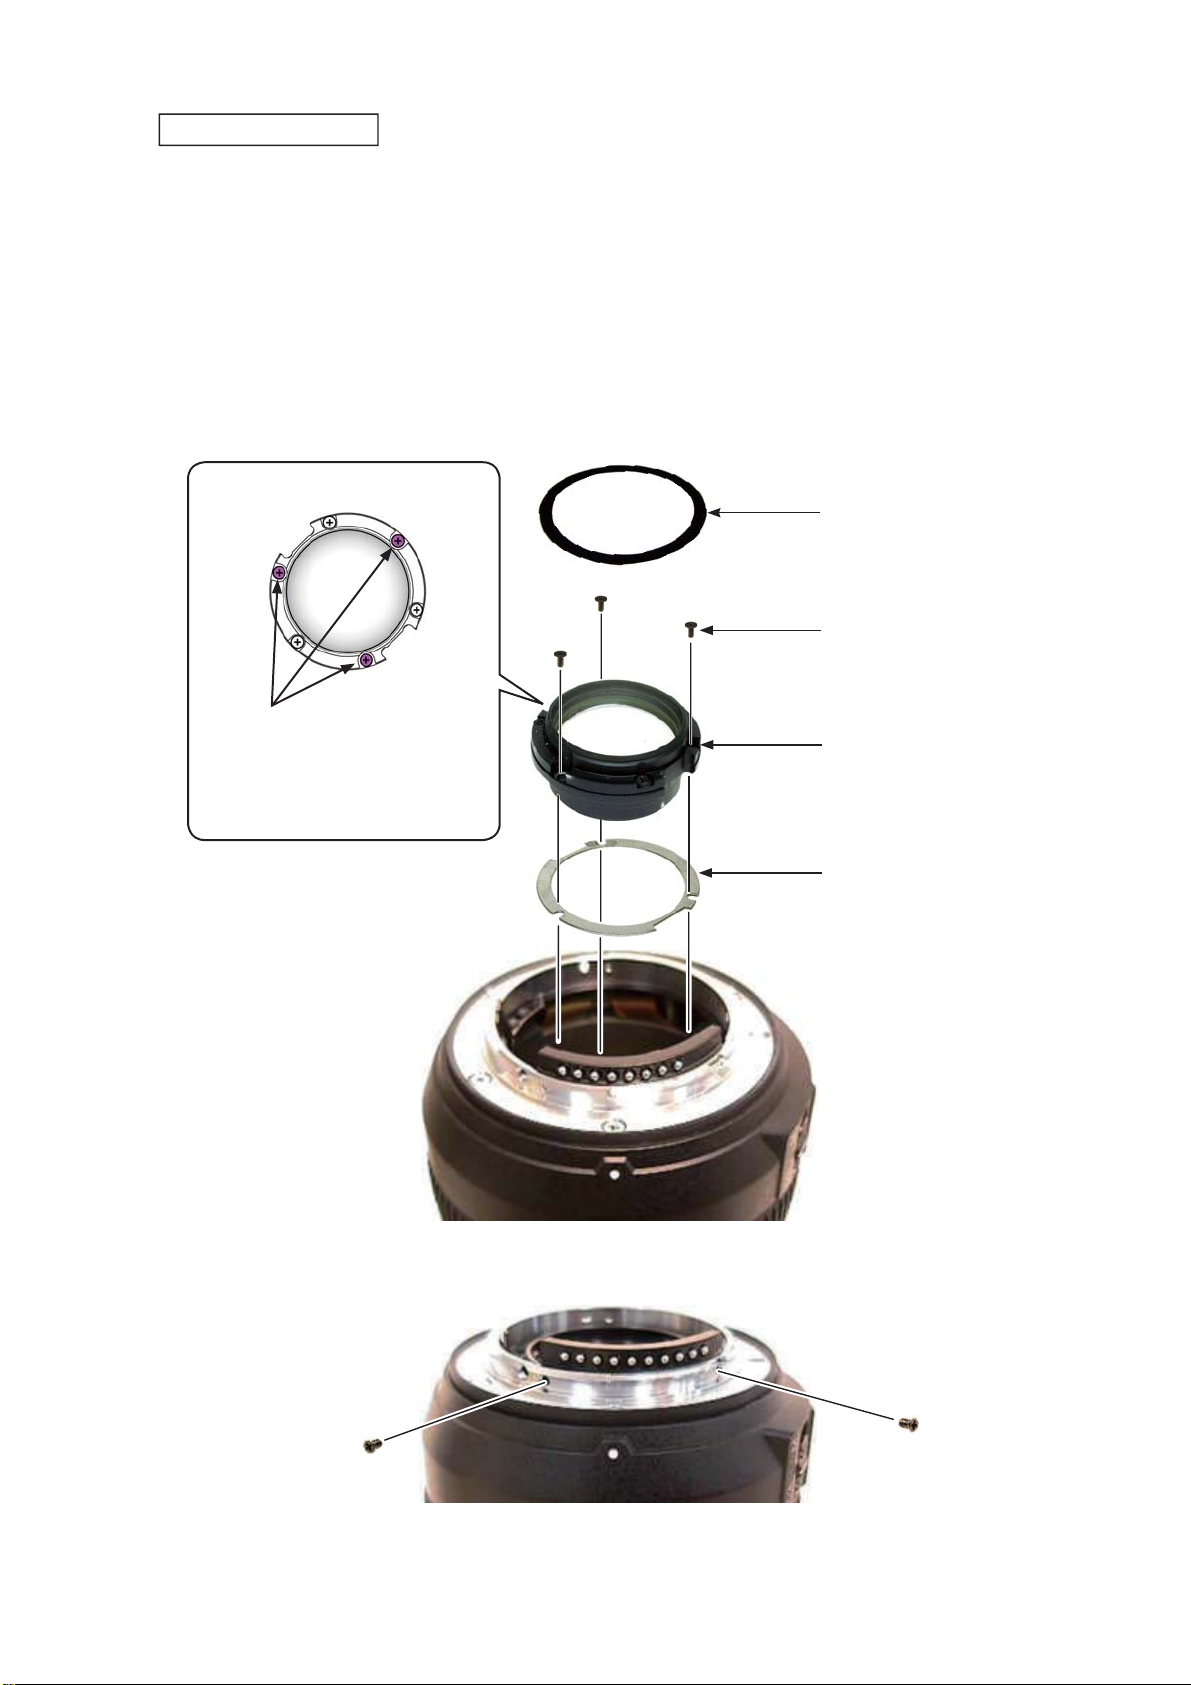
4th lens-group unit
Caution: When the 4th lens-group unit is removed, the lens alignment work will be necessary after assembly.
Therefore, at service facilities where the alignment work can not be performed, do NOT remove the 4th
lens-group unit.
Set the zoom ring to WIDE.
・
Peel off the sheet (#70) from the 4th lens-G unit (B2046).
・
Take out the three screws (#124), and remove the 4th lens group unit (B2046) and washer (#139).
・
Top view
#70
#124×3
Caution
Lens alignment is made for the 4th
lens-G unit, so do NOT touch the
three screws (#125).
B2046
#139
Take out the two screws (#117).
・
#117×2
- D7・AF-S DX 16-85/3.5-5.6G VR -
Page 9
JAA80051-R.3741.A
INC
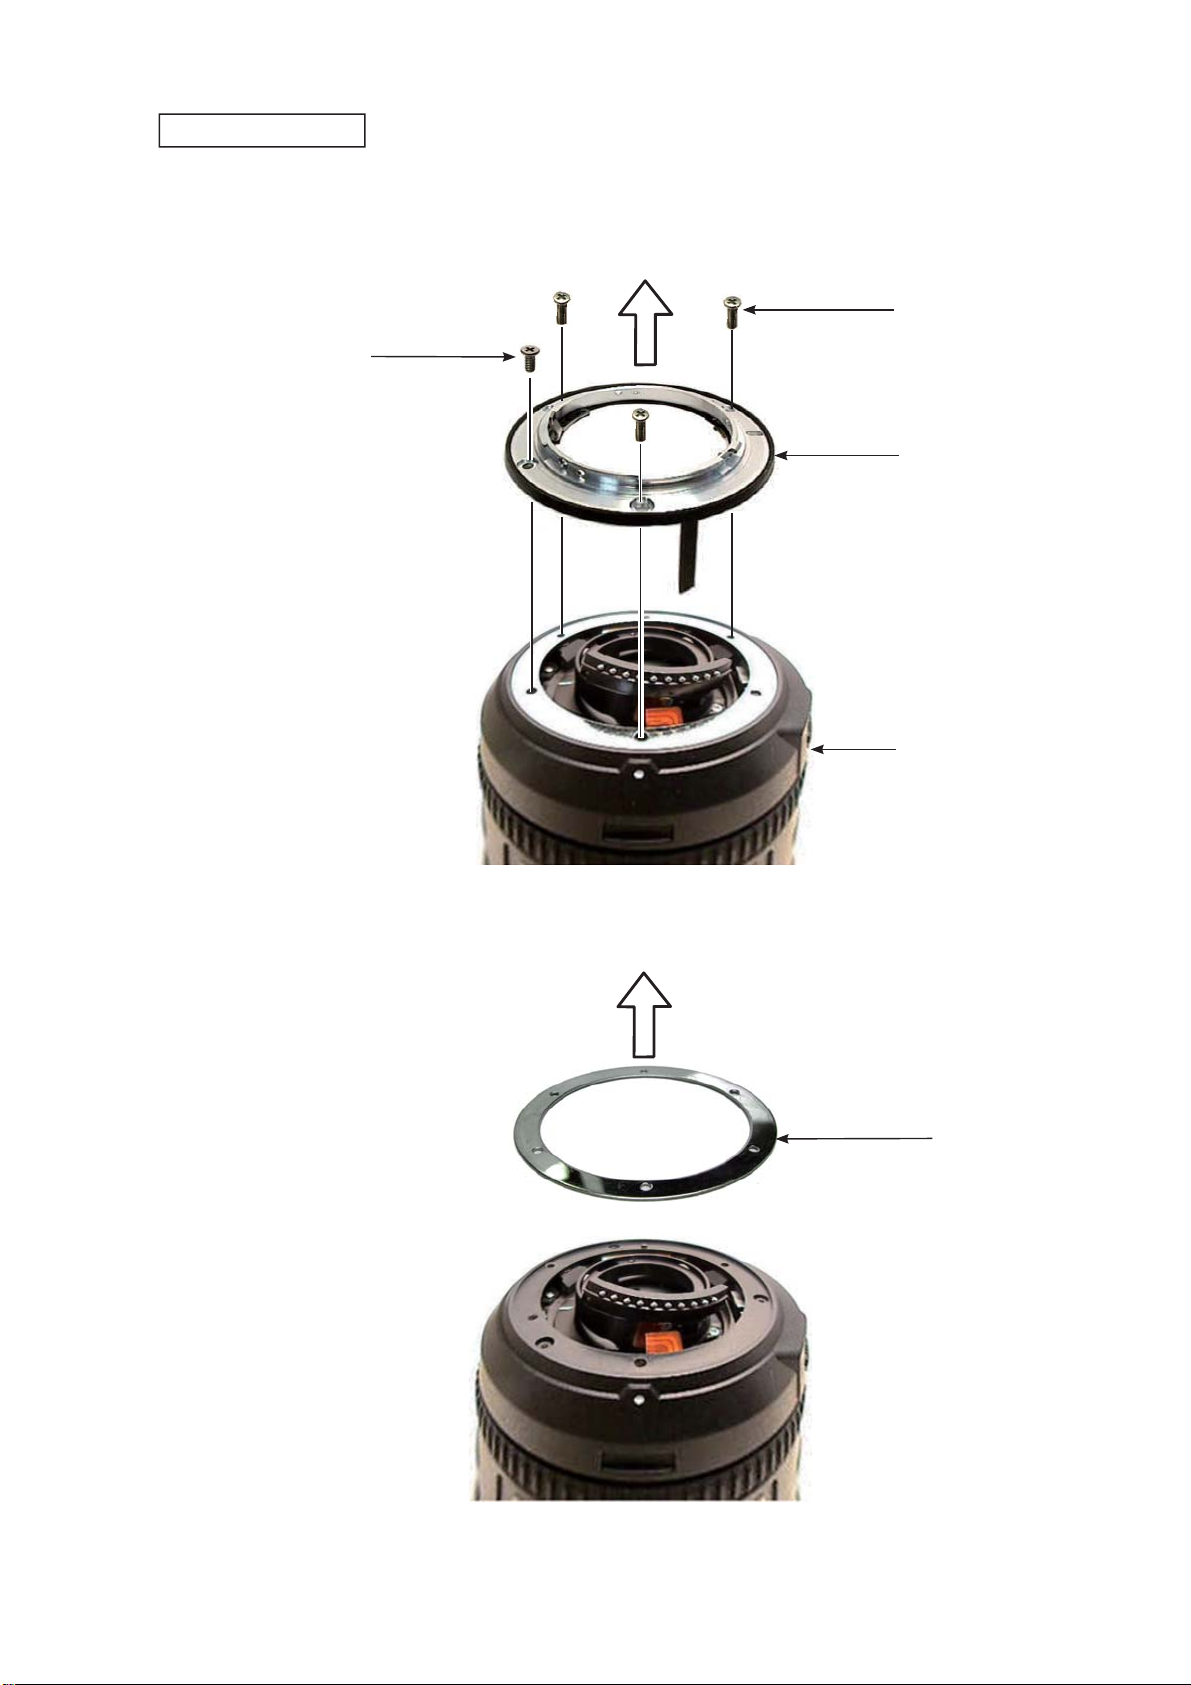
Bayonet mount unit
Take out the three screws (#115) and the one screw (#114), and remove the bayonet mount unit (B30).
・
#115×3
#114
B30
B29
Caution:
Do NOT remove the bayonet mount unit (B30) and the rear fi xed tube unit (B29) together.
The main PCB is connected by the FPC of the rear fi xed tube (B29), so do NOT pull the FPC by force.
Otherwise the FPC will be damaged.
Remove the washer (#79).
・
#79
- D8・AF-S DX 16-85/3.5-5.6G VR -
Page 10
JAA80051-R.3741.A
INC
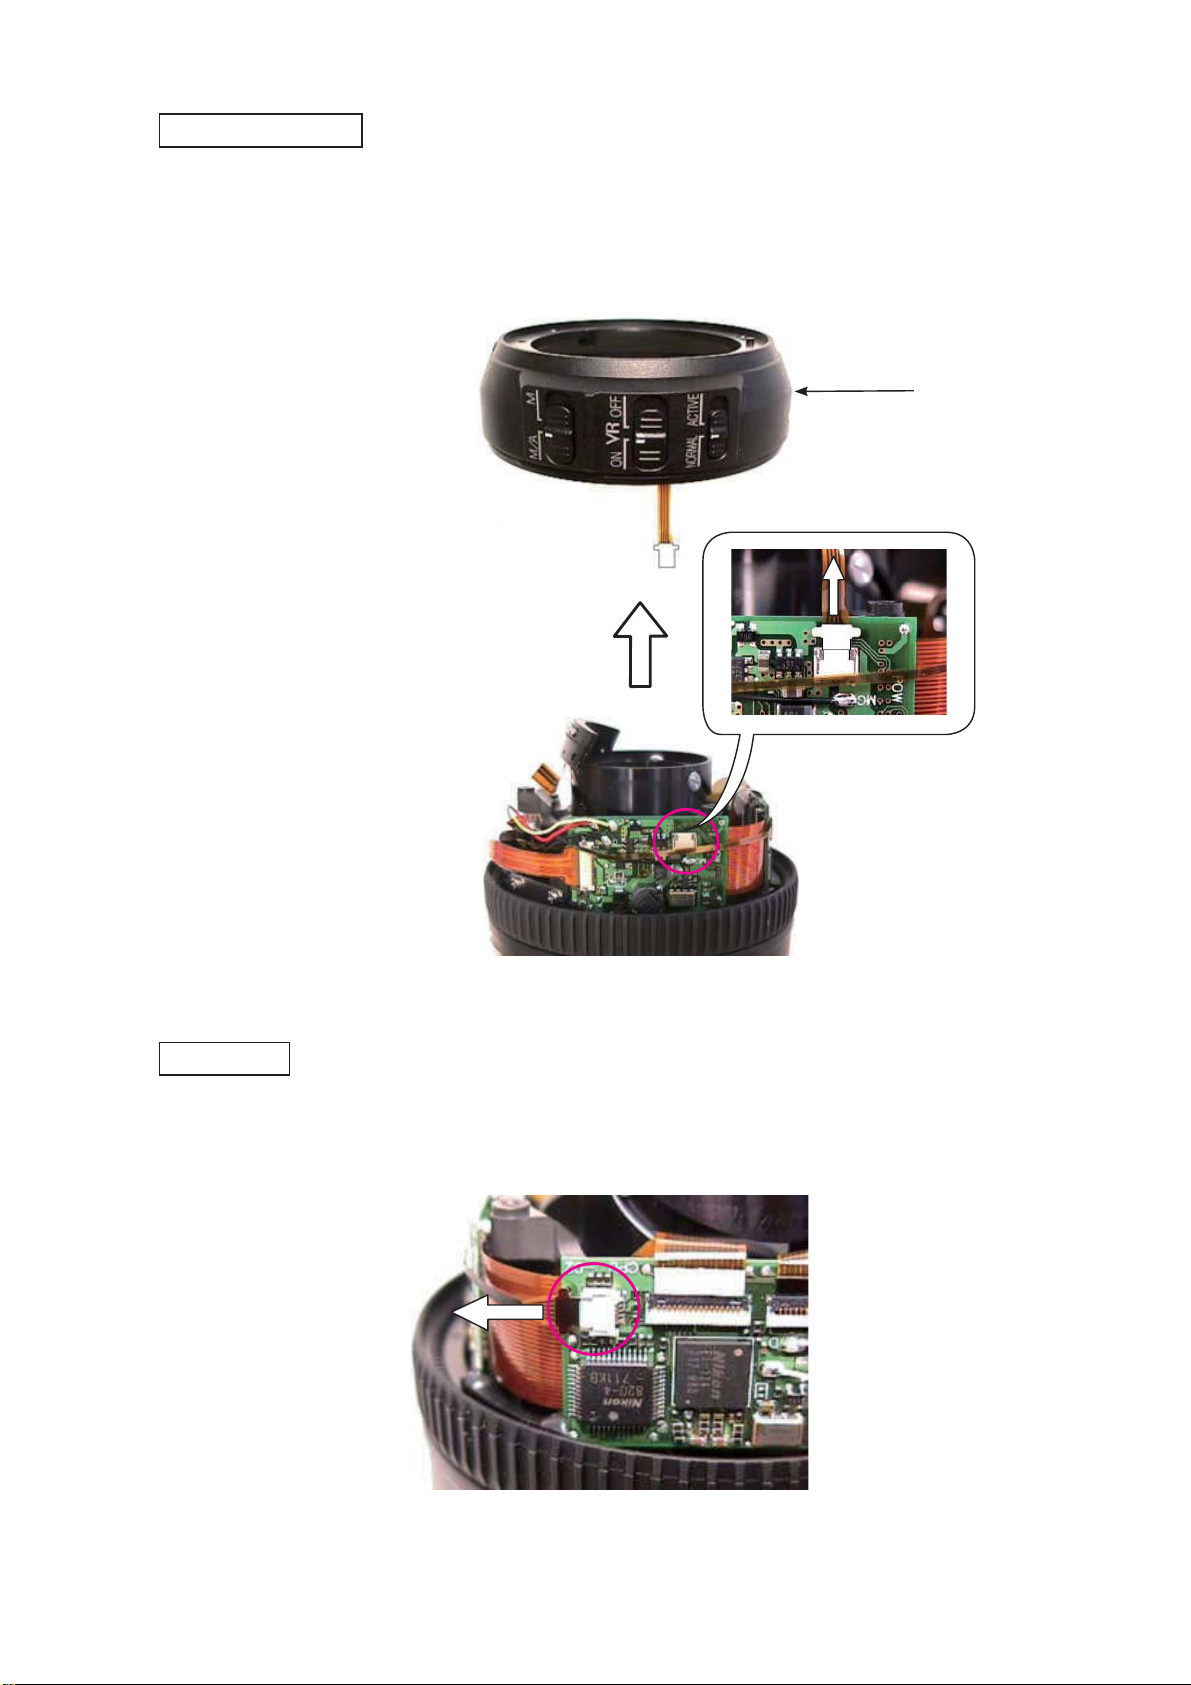
Rear fi xed tube unit
Disconnect the FPC of the rear fi xed tube unit (B29) from the connector of the main PCB (B1001).
・
Remove the rear fi xed tube unit (B29).
・
B29
Main PCB
Disconnect the FPC of GMR unit (#1011) from the connector of the main PCB (B1001).
・
- D9・AF-S DX 16-85/3.5-5.6G VR -
Page 11
JAA80051-R.3741.A
INC
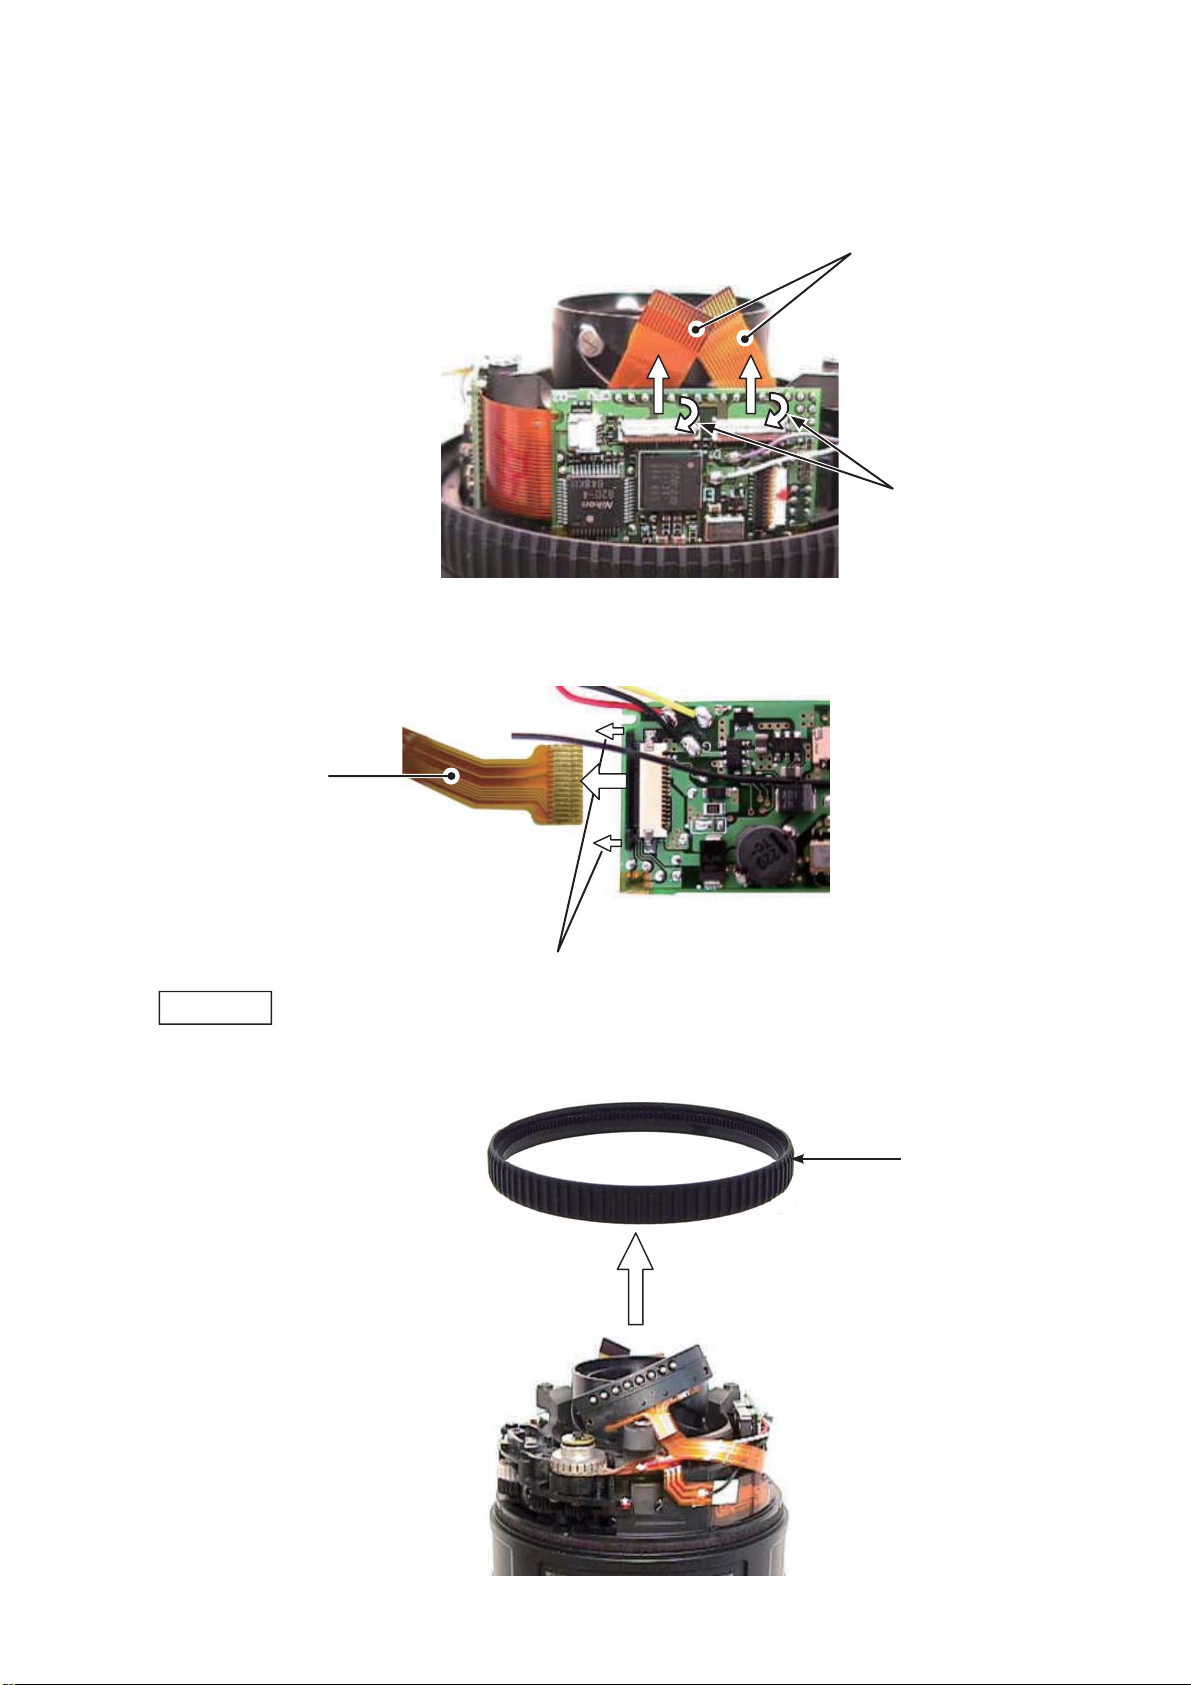
Disconnect the connection-FPC (#1001) from the connector of the main PCB (B1001).
・
Caution:
Be sure to release the locks of the connector before pulling the FPCs.
Disconnect the FPC of the contact unit (B1007) from the connector of the main PCB (B1001).
・
#1001
Release lock here.
B1007
MF ring
Remove MF ring (#26).
・
Caution:
Be sure to release the locks of the connector before pulling the FPCs.
#26
- D10・AF-S DX 16-85/3.5-5.6G VR -
Page 12
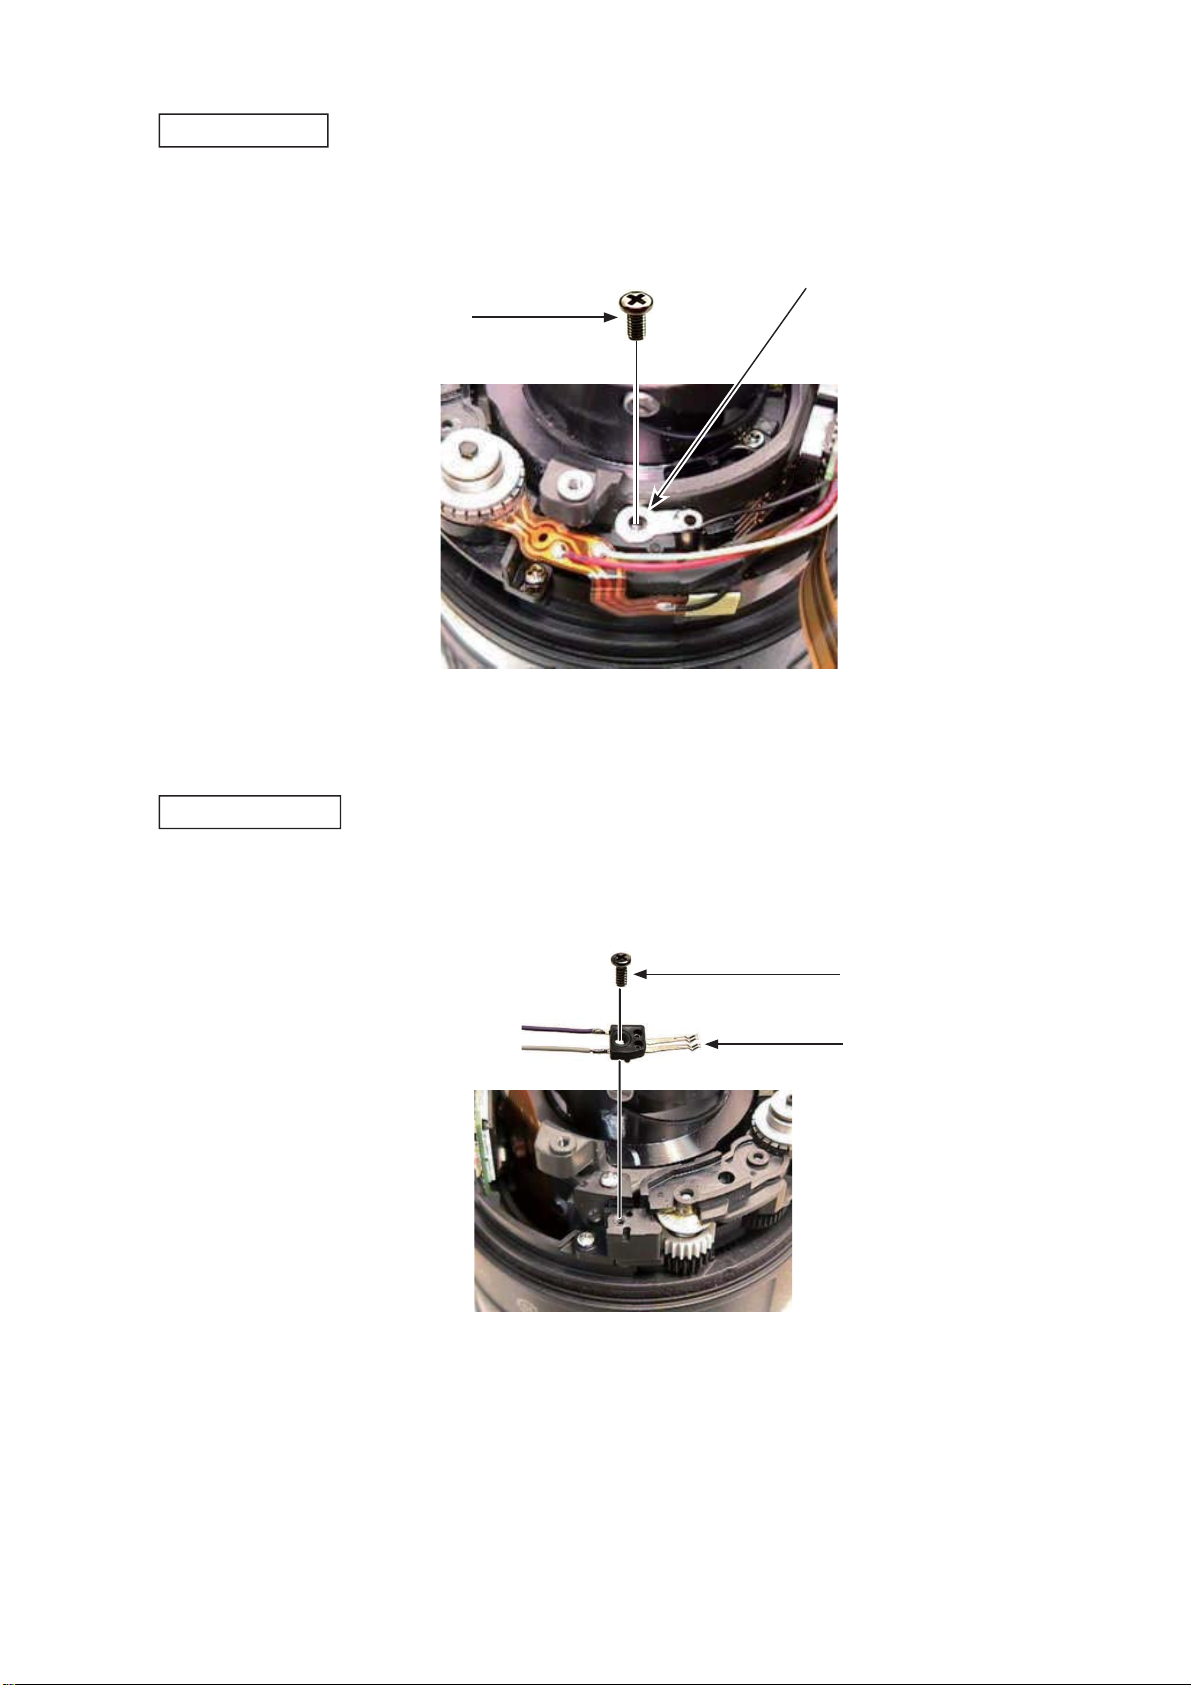
Lug plate unit
INC
Take out the screw (#123), and remove the lug plate unit (B1028).
・
#123
JAA80051-R.3741.A
B1028
MF brush unit
Take out the screw (#587),and remove MF brush unit (#2533) from SWM unit.
・
#587
#2533
- D11・AF-S DX 16-85/3.5-5.6G VR -
Page 13
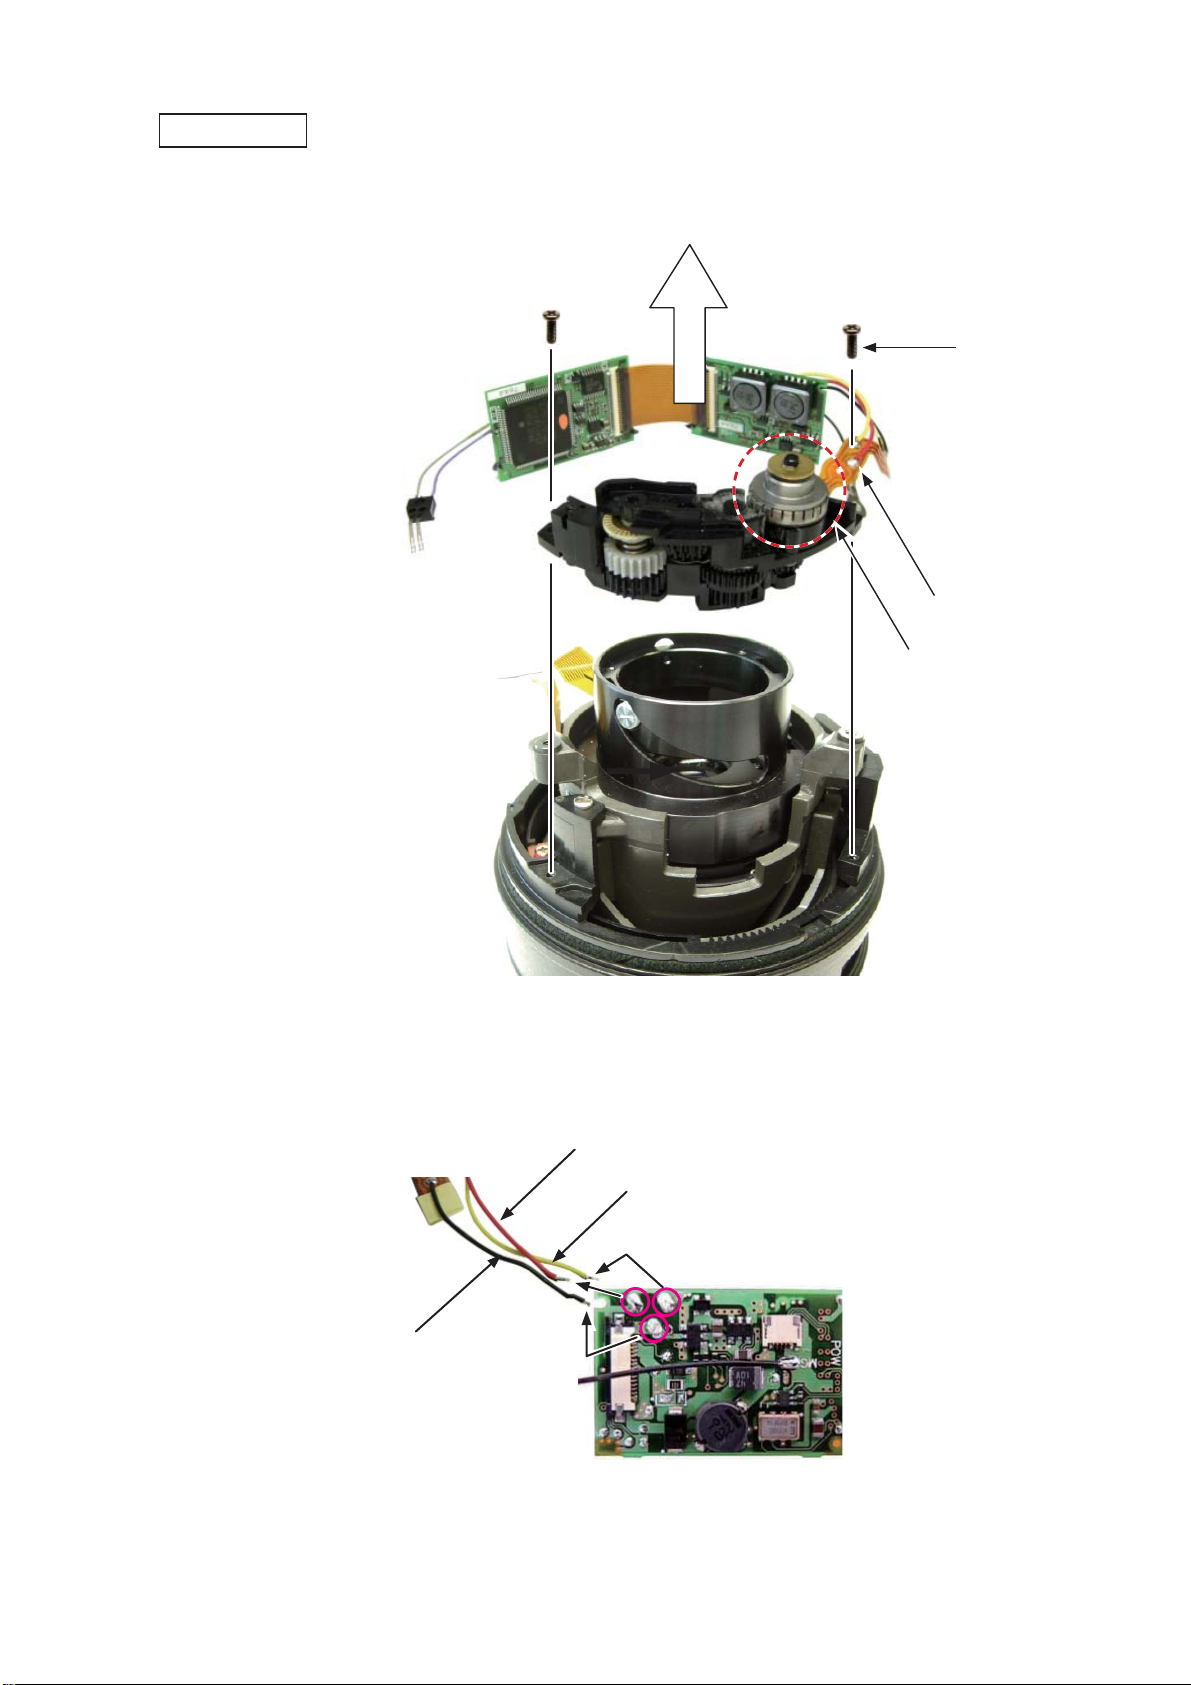
SWM unit
INC
Take out the two screws (#145), and remove SWM unit and main PCB (B1001).
・
Caution: Do NOT touch "A" area.
JAA80051-R.3741.A
#145×2
Back side has double-
stick tape attached
Remove the three lead wires of SWM unit from the main PCB (B1001).
・
Lead wire (red) (#1029)
Lead wire (yellow)(#1030)
"A" area
Lead wire (black) (#1031)
- D12・AF-S DX 16-85/3.5-5.6G VR -
Page 14
JAA80051-R.3741.A
INC
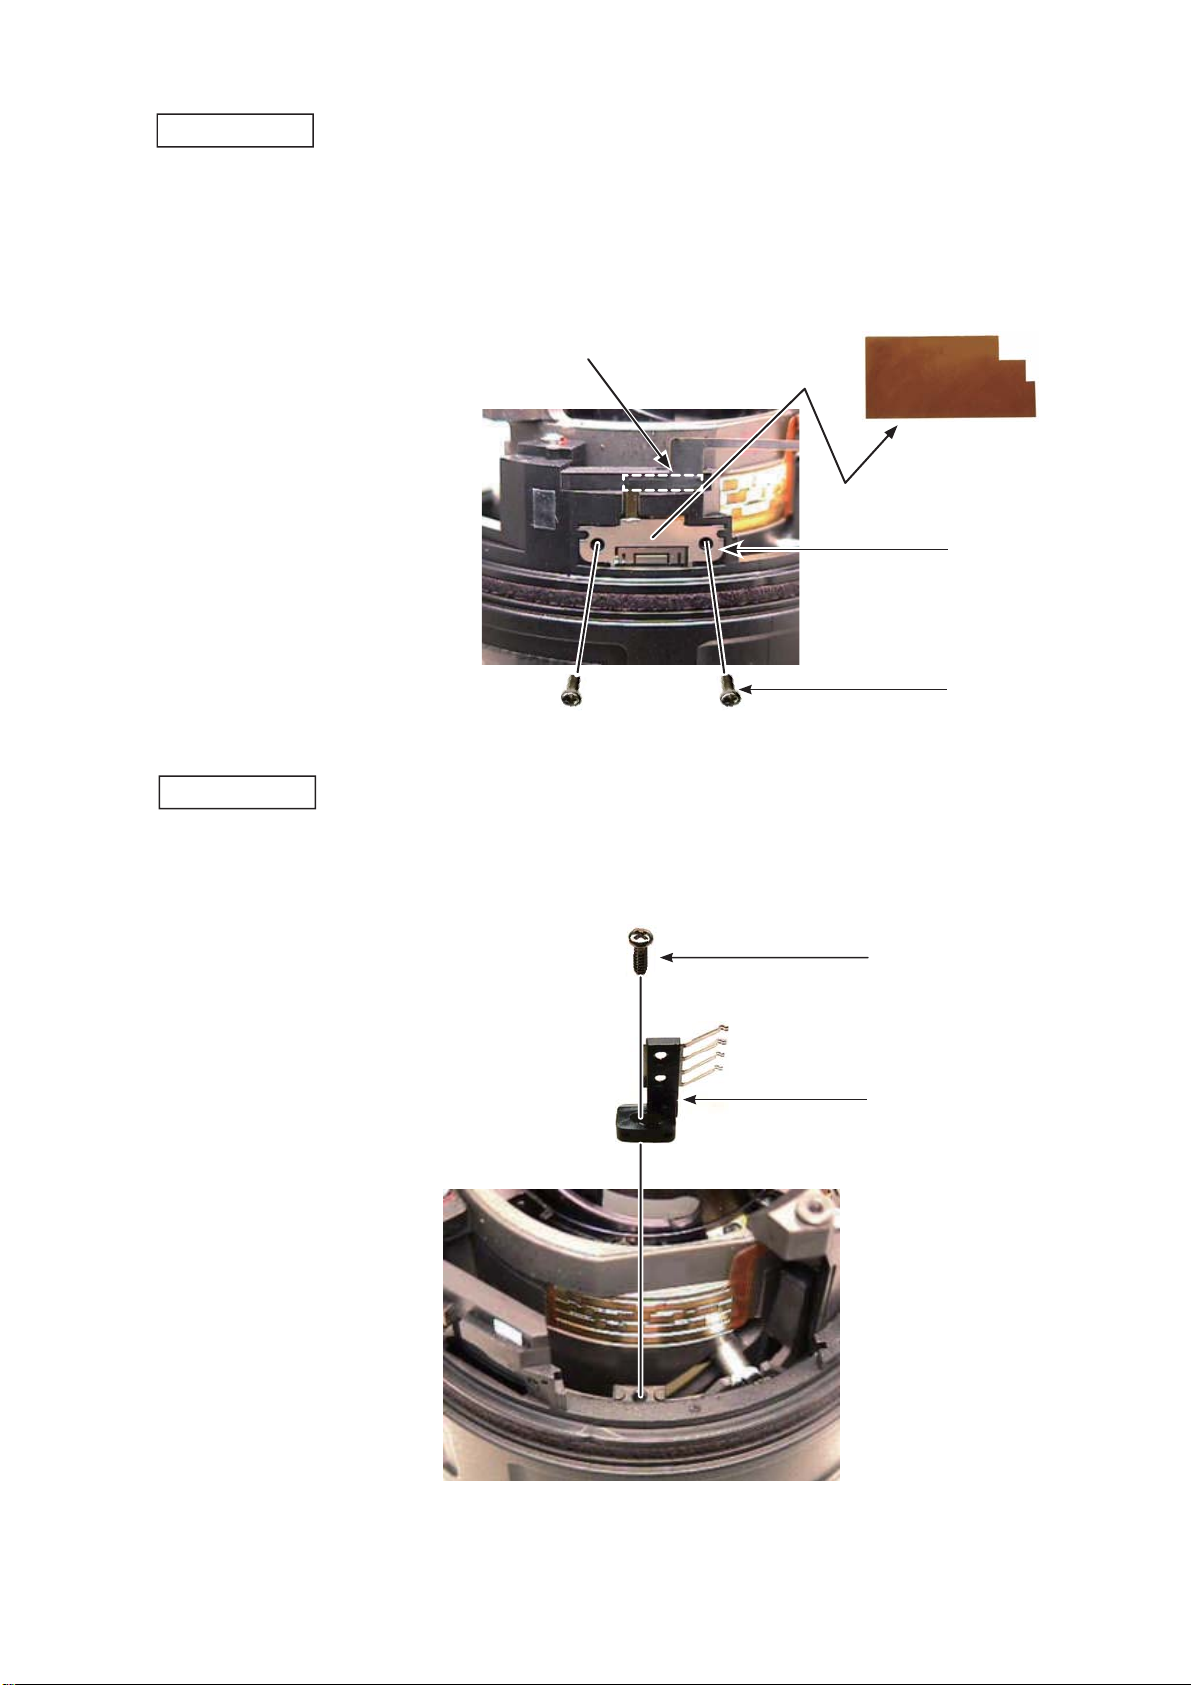
GMR sensor
Peel off the tape (#138).
・
Take out the two screws (#91). Remove the FPC from the double-stick tape and remove GMR sensor
・
(#1011).
#138
Double-stick tape
#1011
Focus brush
Turn the focus brush in the direction of CLOSE.
・
Take out the screw (#145), and remove the focus brush (B105).
・
#91×2
#145
B105
- D13・AF-S DX 16-85/3.5-5.6G VR -
Page 15
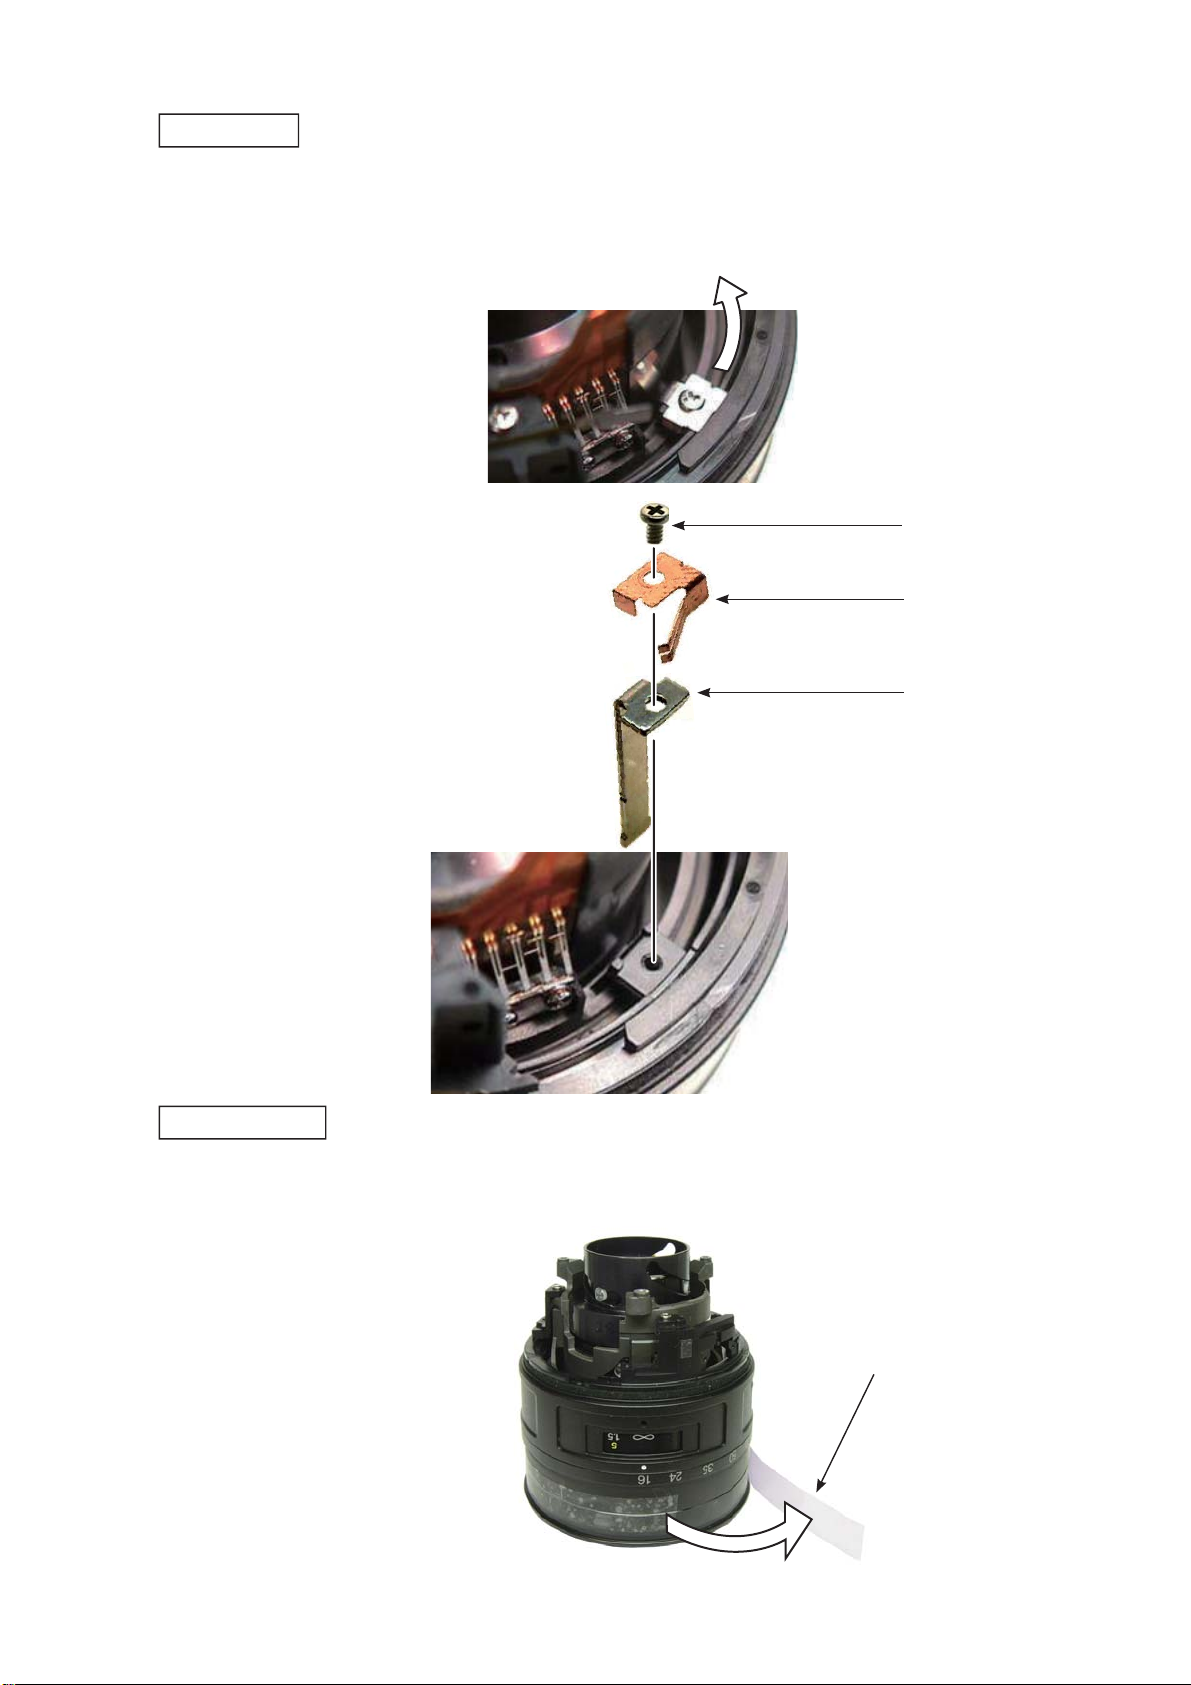
Focus key
INC
Move the key (#54) in the direction of the arrow.
・
Take out the screw (#122), and remove the plate spring (#157) and focus key (#54).
・
JAA80051-R.3741.A
#122
#157
Fixed ring unit
Peel off the tape (#135).
・
#54
#135
- D14・AF-S DX 16-85/3.5-5.6G VR -
Page 16
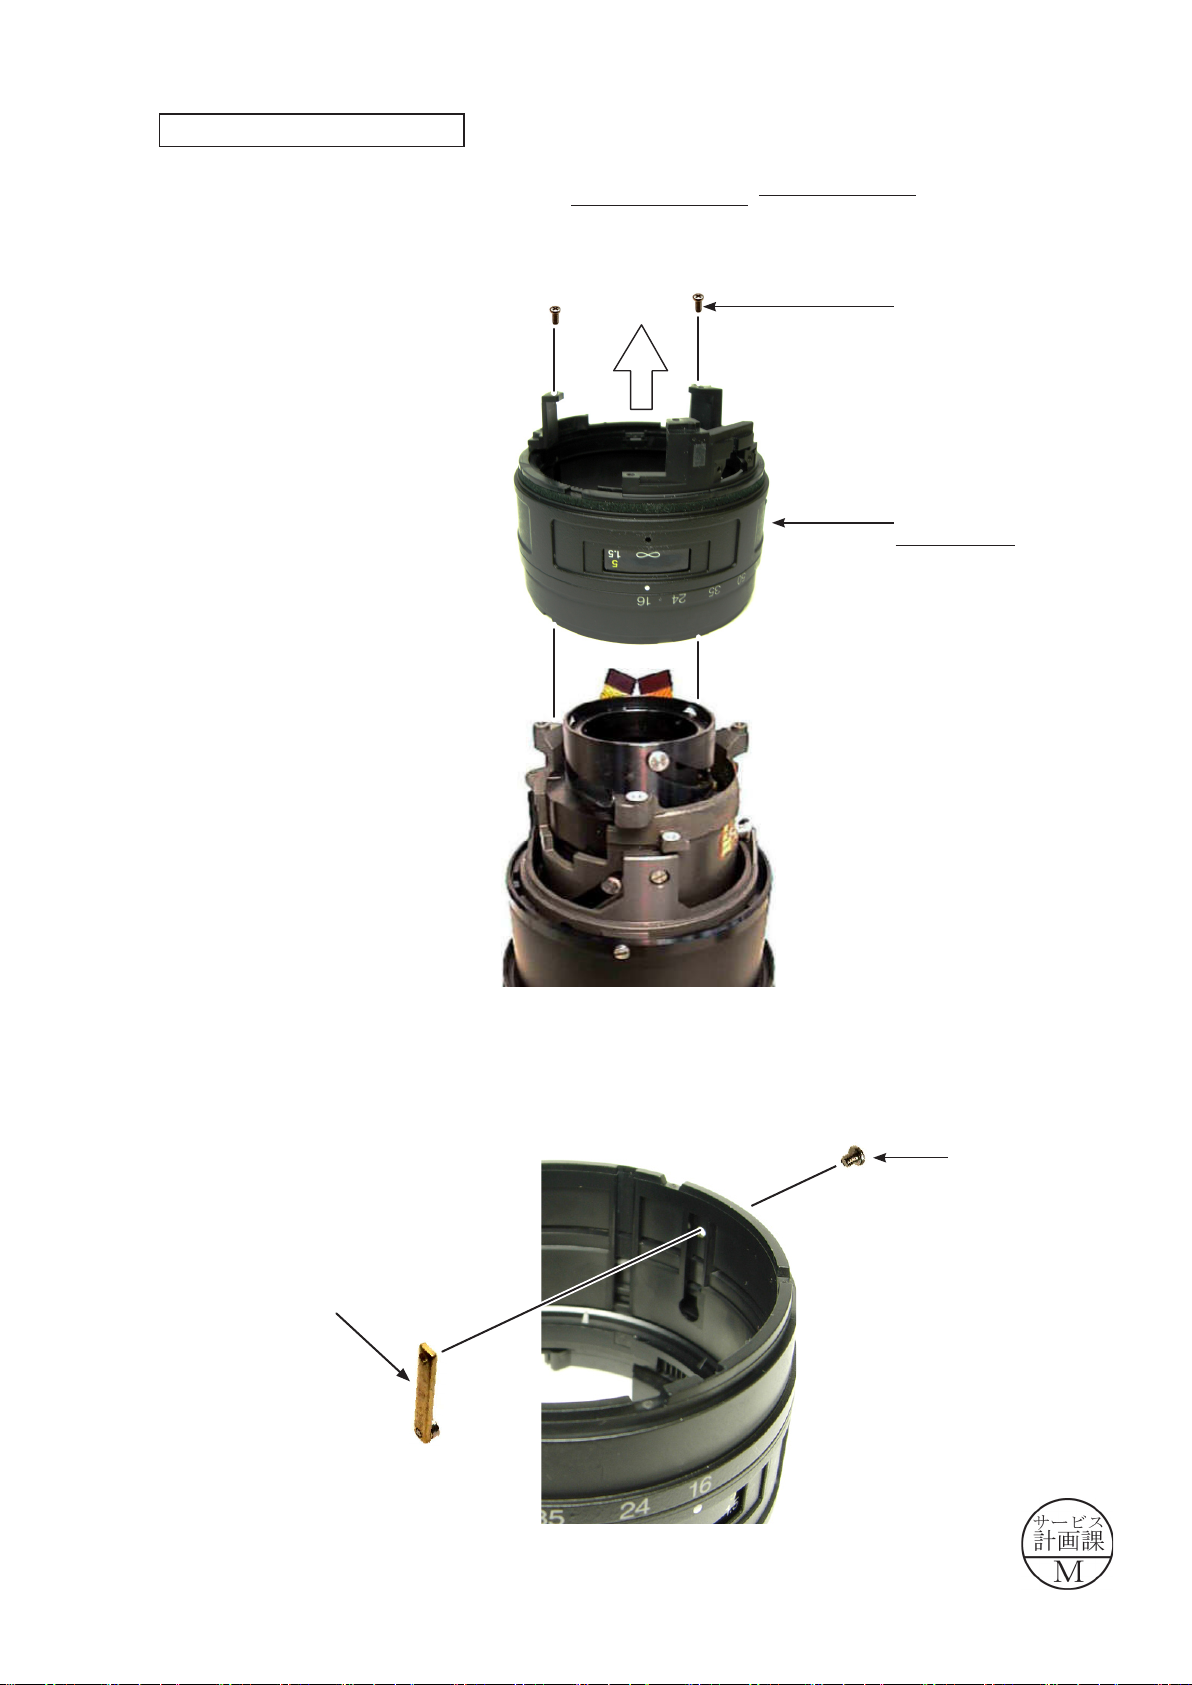
Fixed ring unit (continued)
INC
△ (Revision)
Take out the two screws (#123),and remove the zoom index ring the xed ring unit.
JAA80051-R.3741.A
#123×2
△ (Revision)
Zoom index ring
Fixed ring unit
Take out the screw (#144).
Remove the zoom control key unit (B140) from the xed ring unit.
B140
#144
△× 2
Page 17
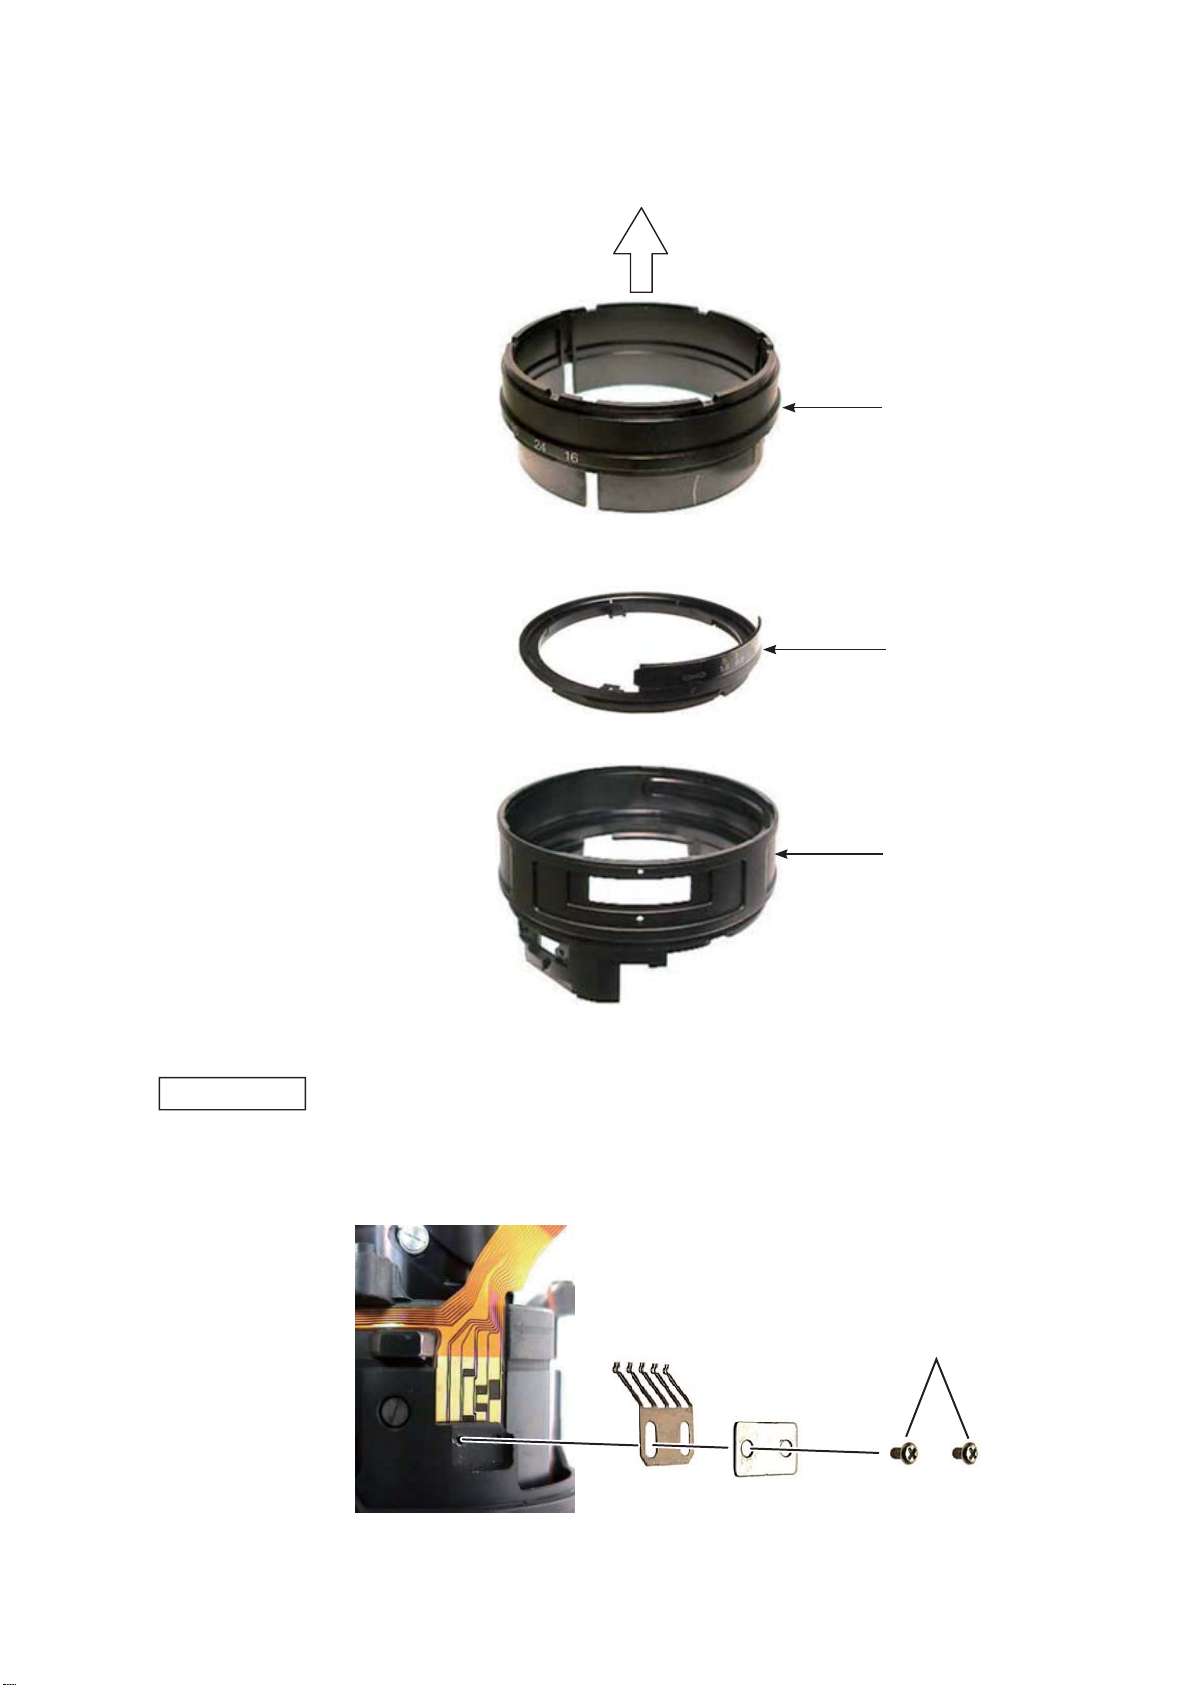
Remove the zoom ring unit (B27) and gear unit (B40) from the fi xed ring (#55).
INC
・
JAA80051-R.3741.A
B27
B40
#55
Zoom brush
Take out the two screws (#109), and remove the reinforcing plate (#106) and zoom brush (#104).
・
#104
#106
#109×2
- D16・AF-S DX 16-85/3.5-5.6G VR -
Page 18
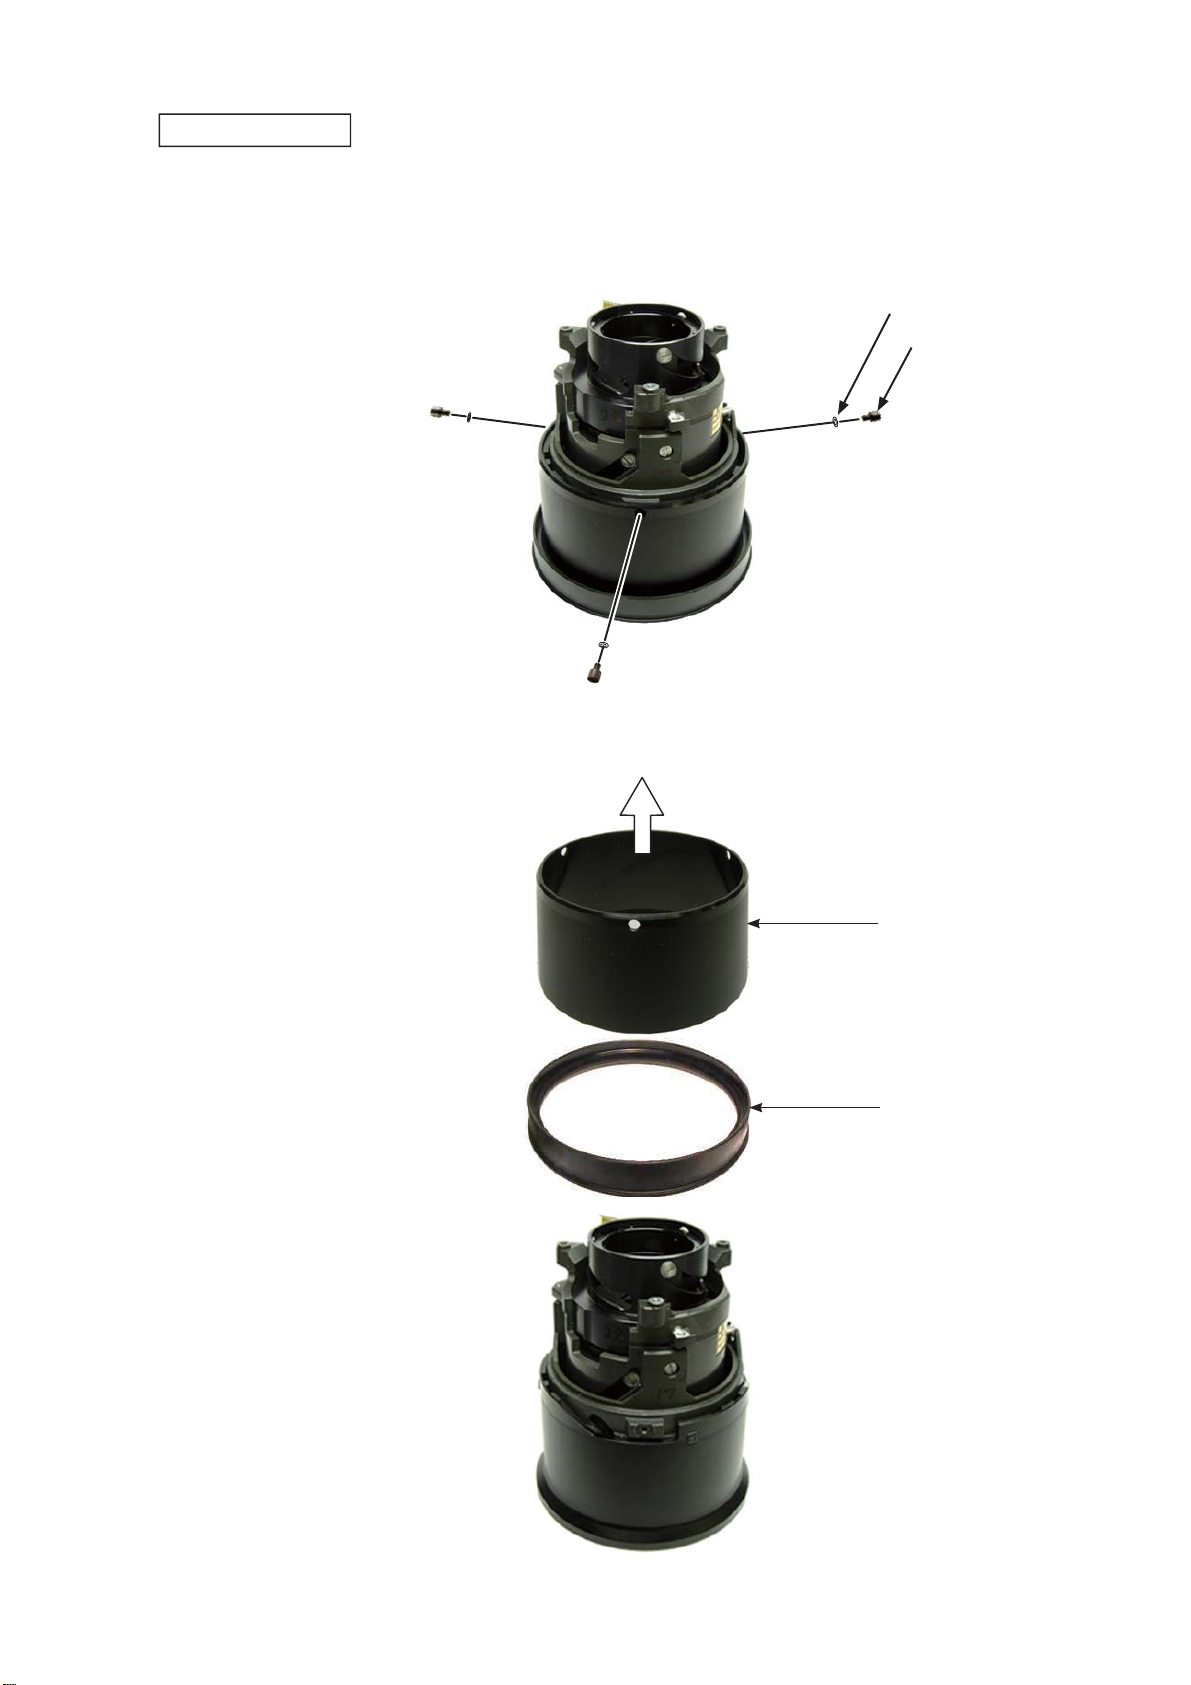
Cover ring unit
INC
Take out the three screws (#110).
・
Take out the screws carefully because sometimes the adjustment washer (#107) is put.
#107 (Adjustment washer)
JAA80051-R.3741.A
#110×3
Remove the cover ring unit (B36) and support ring unit (B101).
・
B36
B101
- D17・AF-S DX 16-85/3.5-5.6G VR -
Page 19
JAA80051-R.3741.A
INC
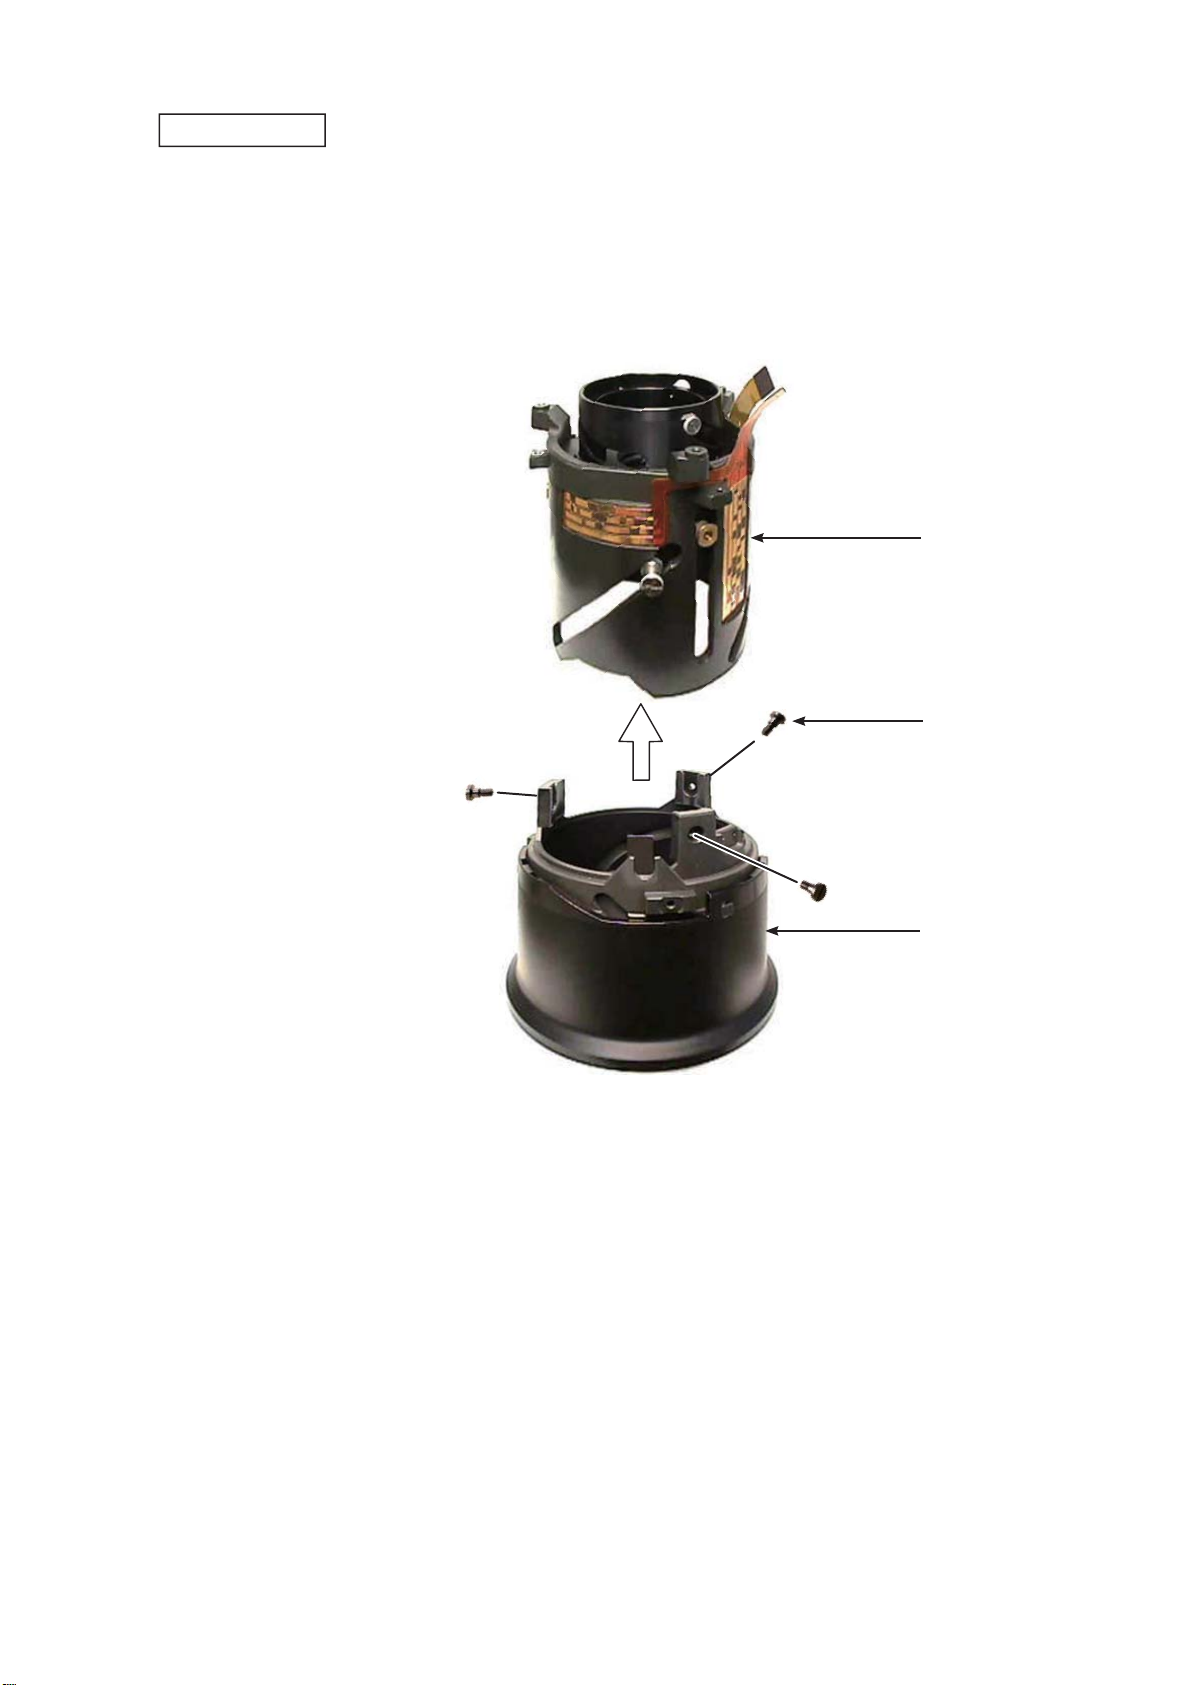
Fixed tube
Take out the three screws (#67), and remove the fi xed tube (#50) from the 2nd lens-G straight ring (B52).
・
#50
#67×3
B52
- D18・AF-S DX 16-85/3.5-5.6G VR -
Page 20
JAA80051-R.3741.A
INC
VR unit-assembly
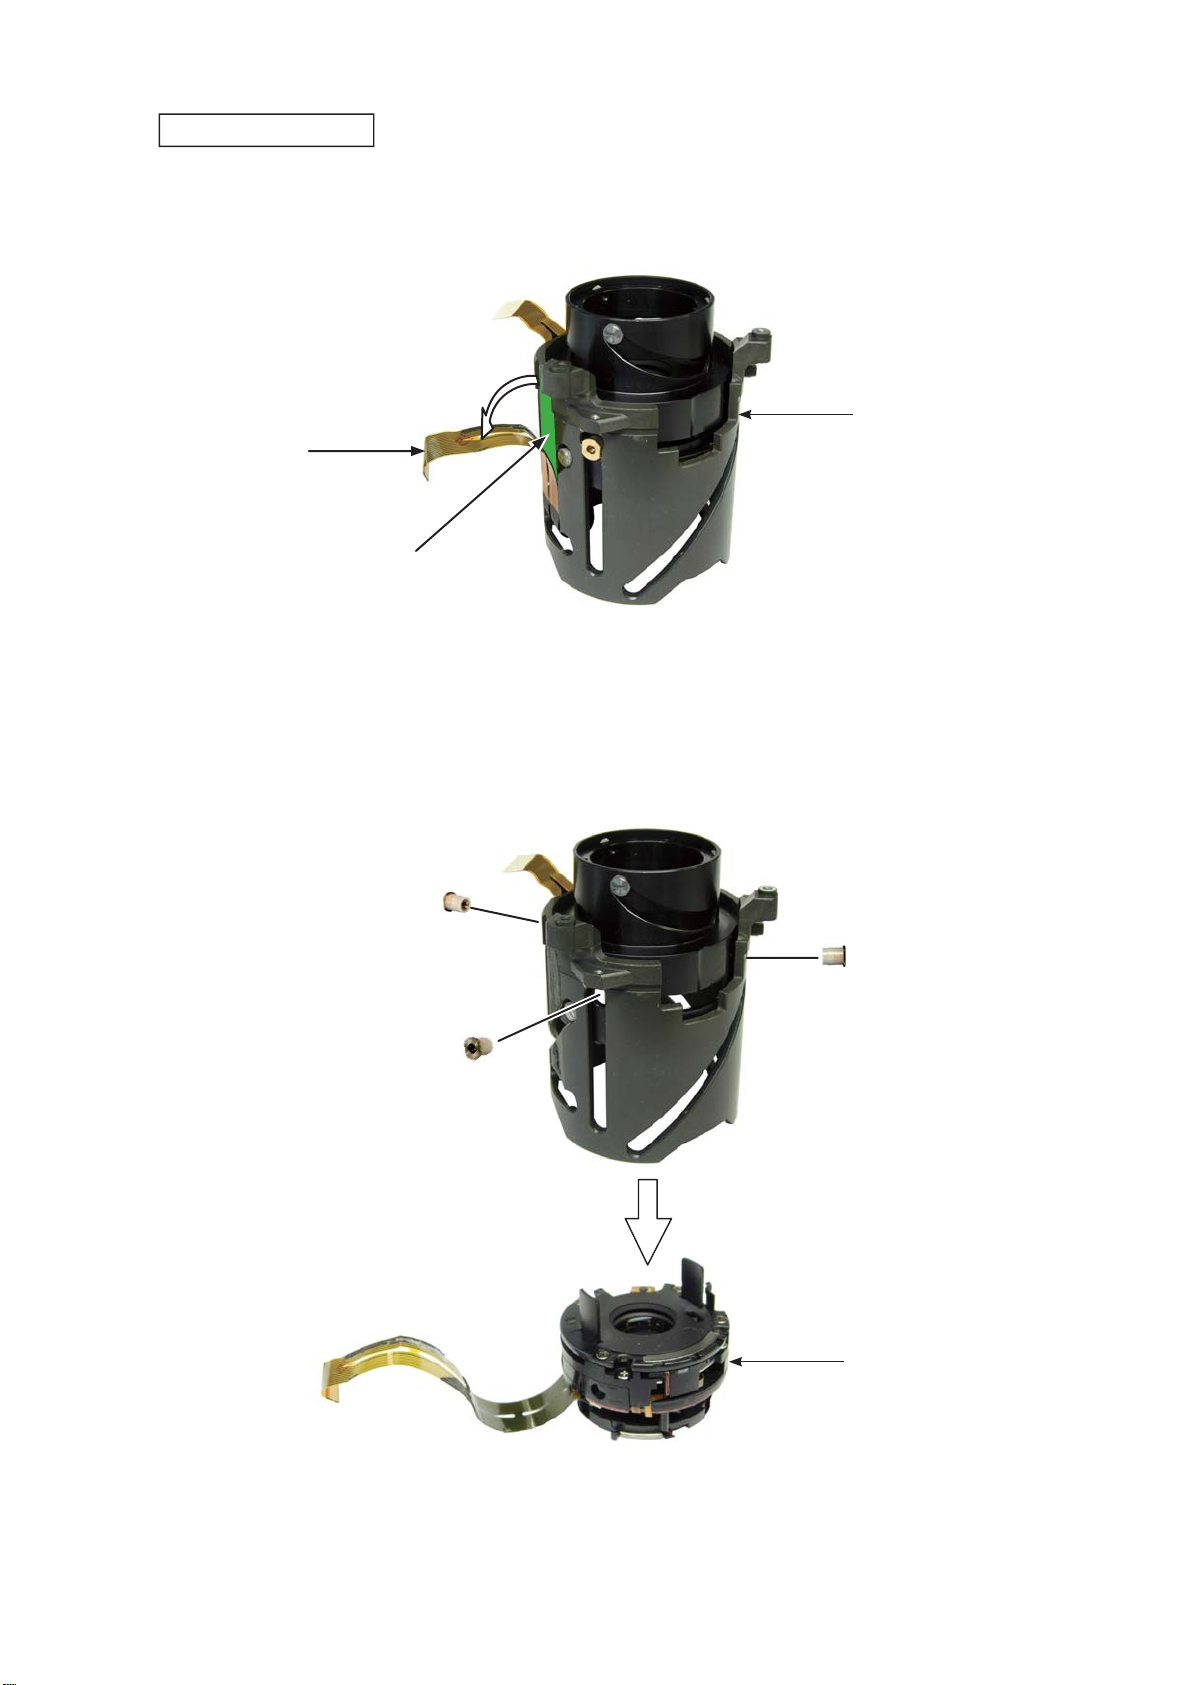
Remove the connection-FPC (#1001) from the double-stick tape adhered to the fi xed tube (#50).
・
#50
#1001
Double-stick tape
Remove the three roller units (B68), and detach VR unit-assembly (B2306).
・
B68×3
B2306
- D19・AF-S DX 16-85/3.5-5.6G VR -
Page 21
JAA80051-R.3741.A
INC
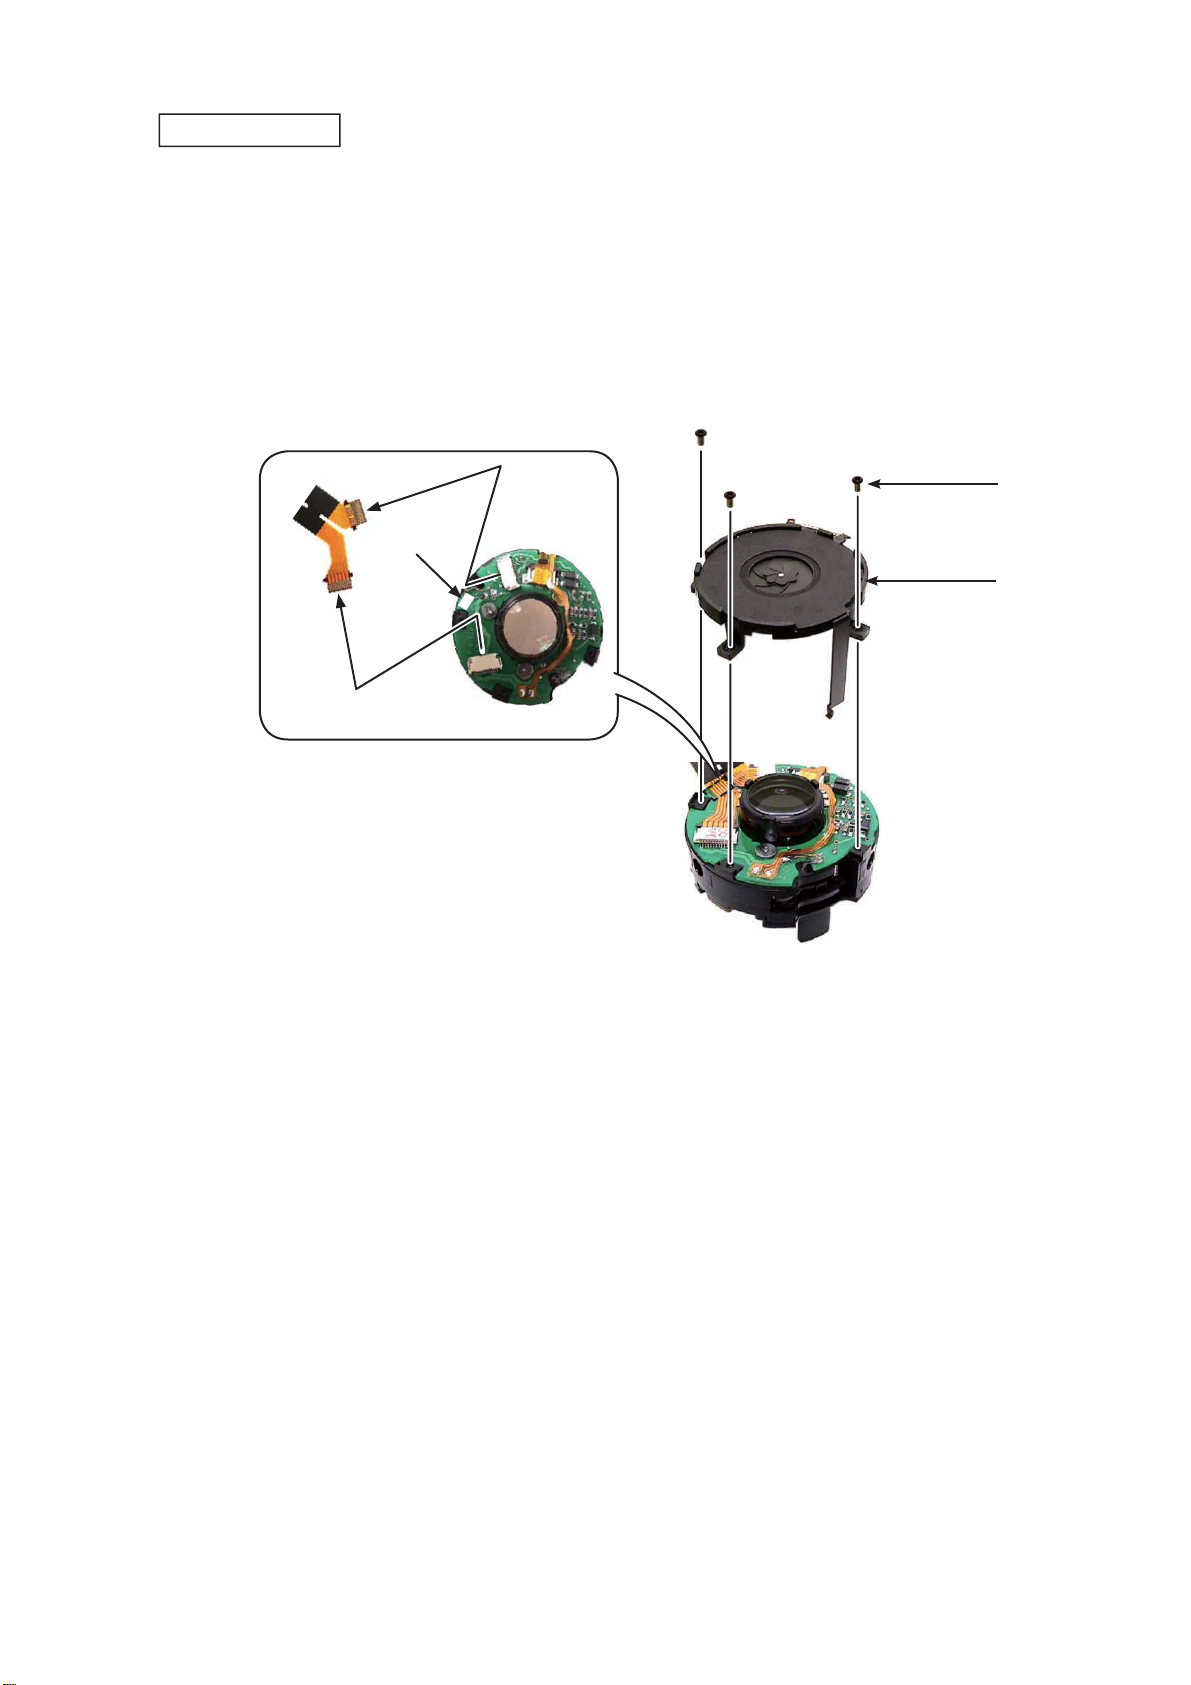
Aperture unit
Take out the three screws (#56), and remove the aperture unit (B34).
・
Remove the connection-FPC (#1001) from the double-stick tape, and disconnect it from the connector of VR
・
unit in numeric order from ① to ②.
#1001
①
②
Double-stick
tape
#56×3
B34
- D20・AF-S DX 16-85/3.5-5.6G VR -
Page 22
JAA80051-R.3741.A
INC
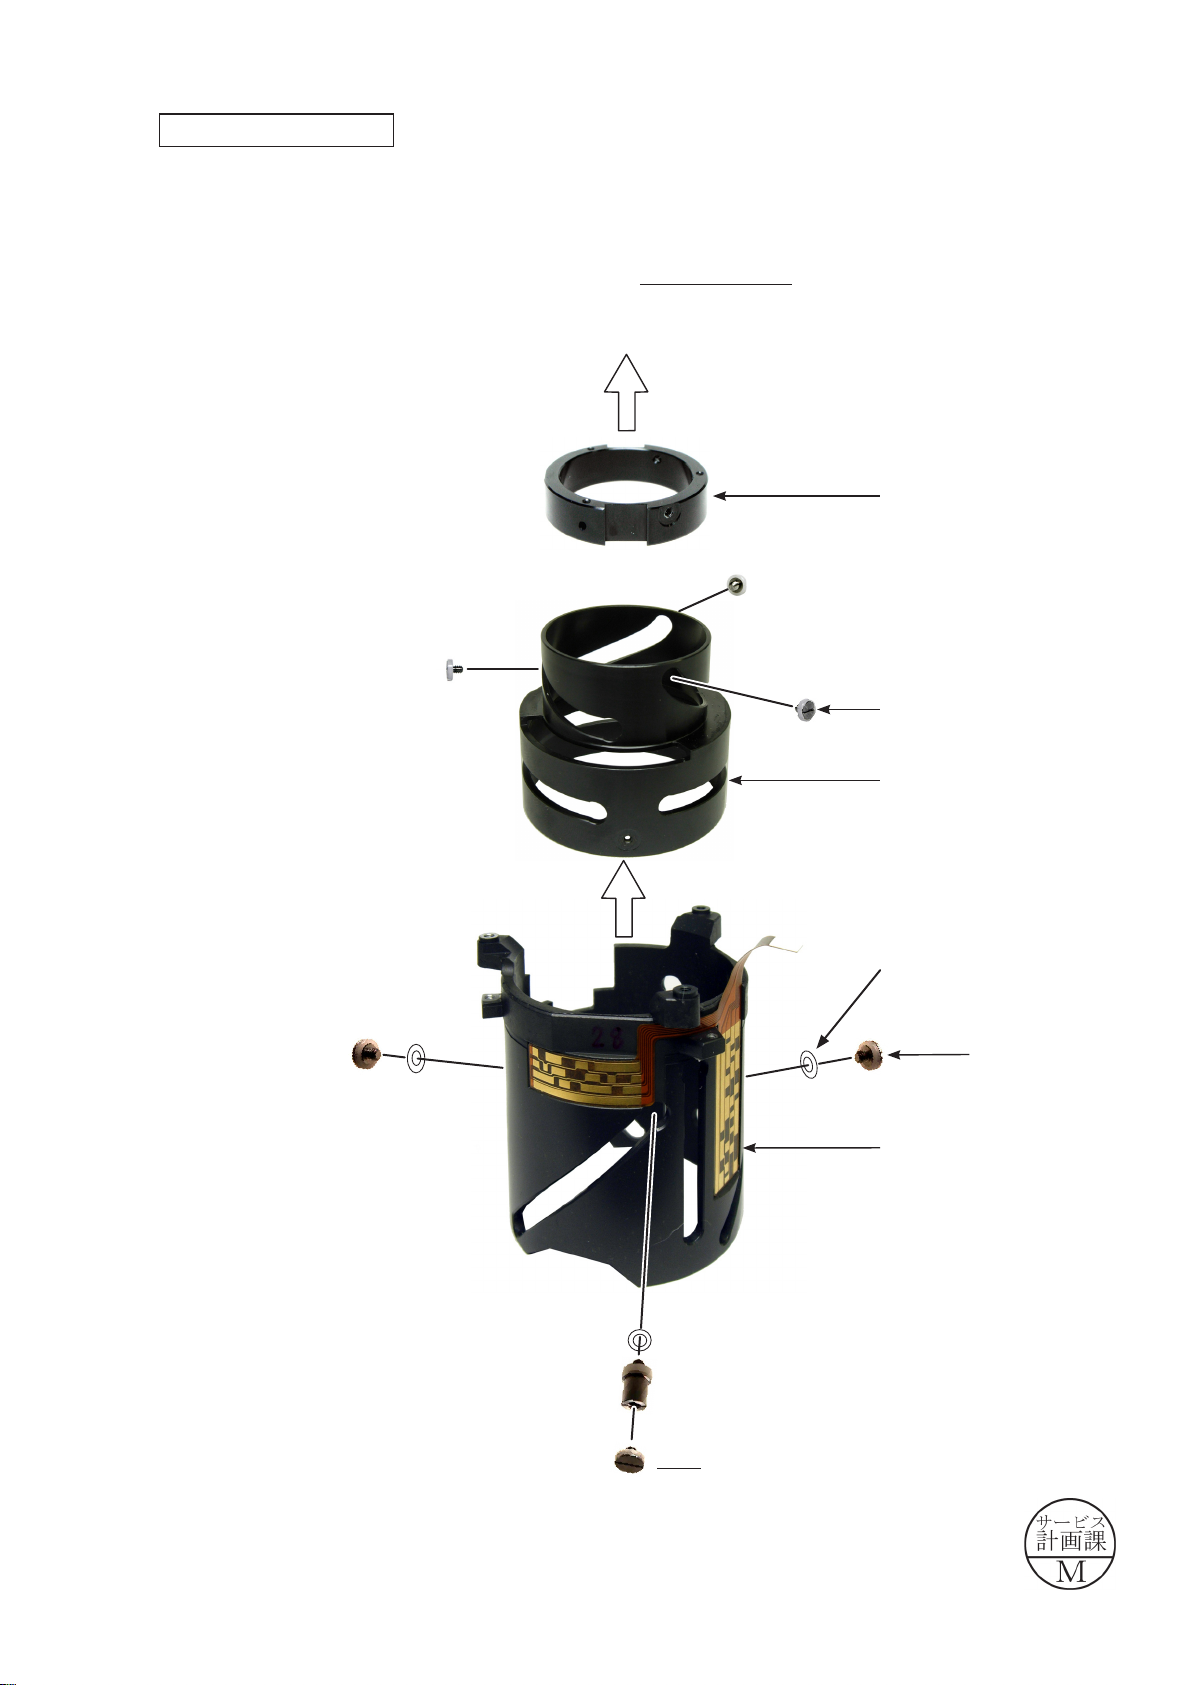
4th lens-G sliding ring
Remove the three roller units (B81), and remove the 4th lens-G sliding ring (#48) from the 3-4 lens-G cam
ring (#24).
Remove the two roller units (B83), roller unit (B99), roller unit (B102) and three washers (#82), then remove
△ (Addition)
the 3-4 lens-G cam ring (#24) from the xed tube (#50).
#48
B81×3
#24
#82×3
#50
B83×2
△× 2
B99
△ (Addition)
B102
Page 23
JAA80051-R.3741.A
INC
2. Assembly / Adjustment
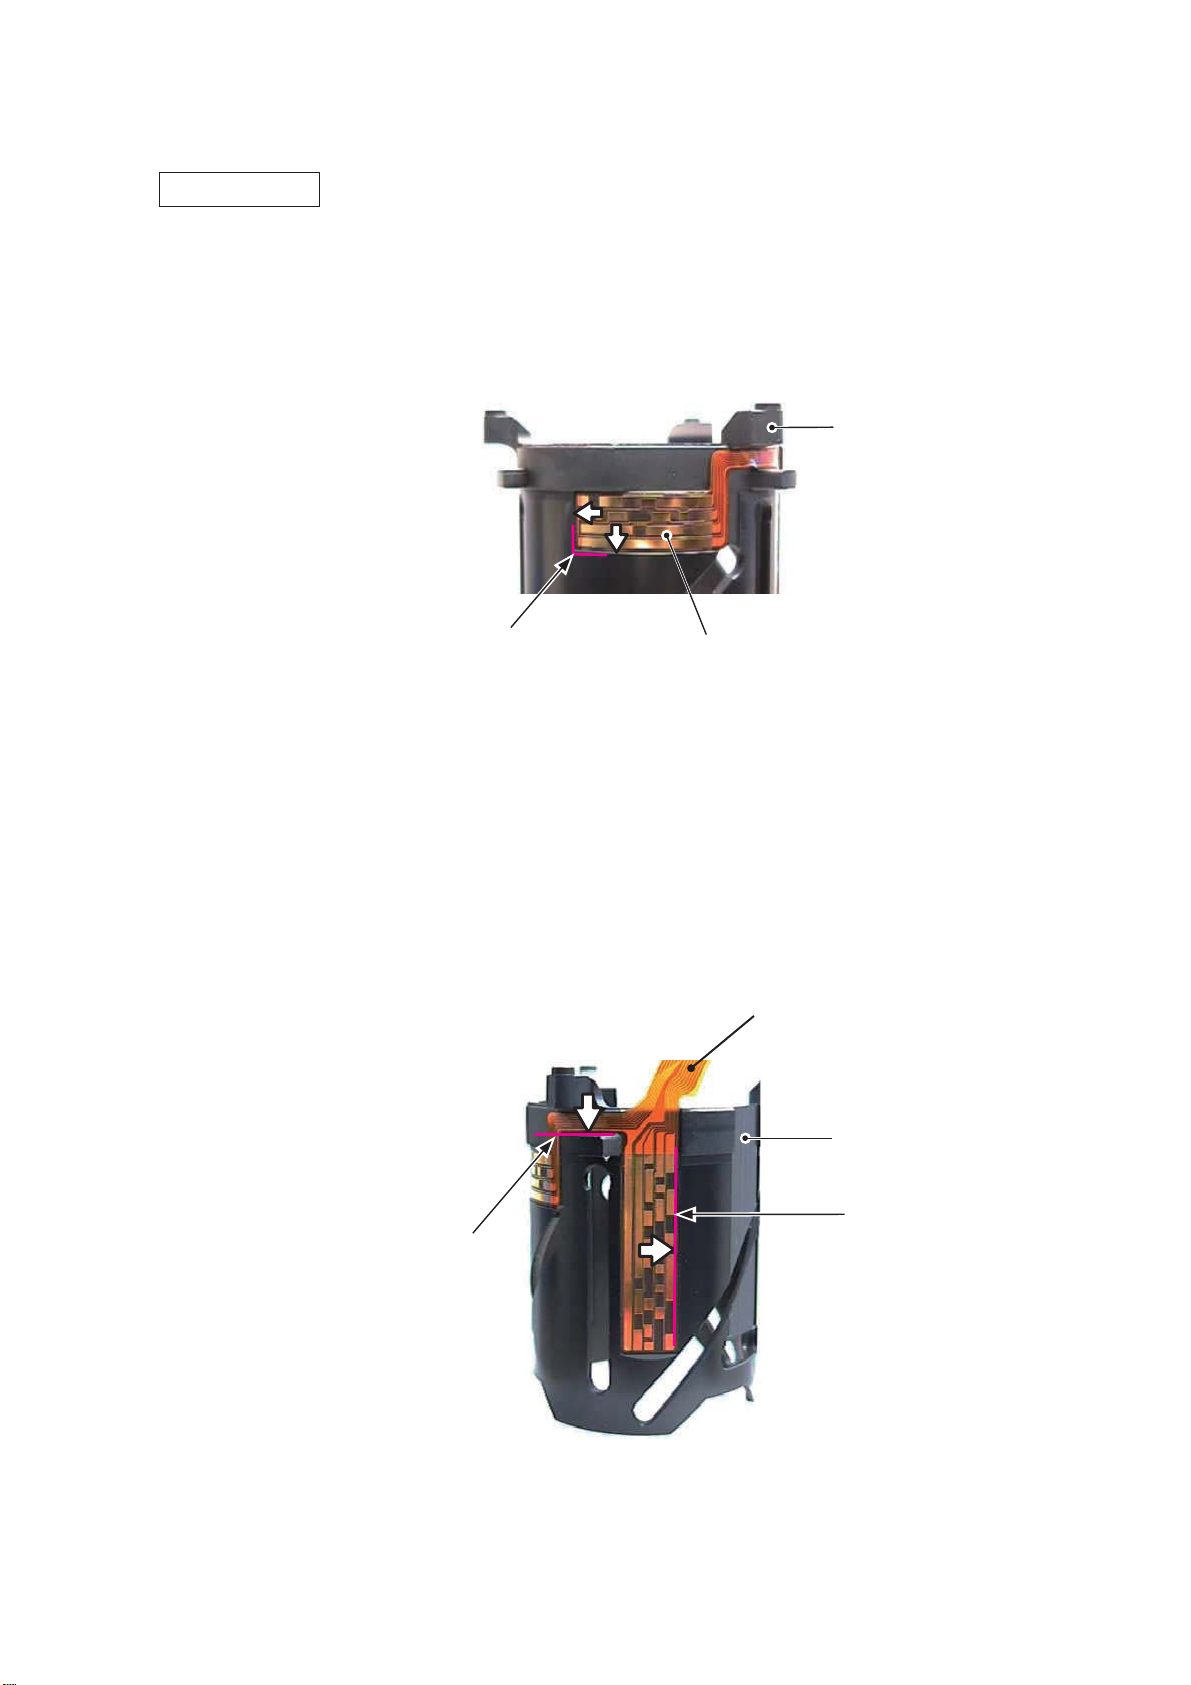
Encoder FPC
Place the encoder-FPC (#1006) on the fi xed tube (#50) based on the below reference position, and attach it
・
by pressing in the direction of the arrow for positioning.
#50
Reference position
Place the encoder-FPC (#1006) on the fi xed tube (#50) based on the below reference position each, and
・
attach it by pressing in the direction of the arrow for positioning.
Reference position
#1006
#1006
#50
Reference position
- A1・AF-S DX 16-85/3.5-5.6G VR -
Page 24
JAA80051-R.3741.A
INC
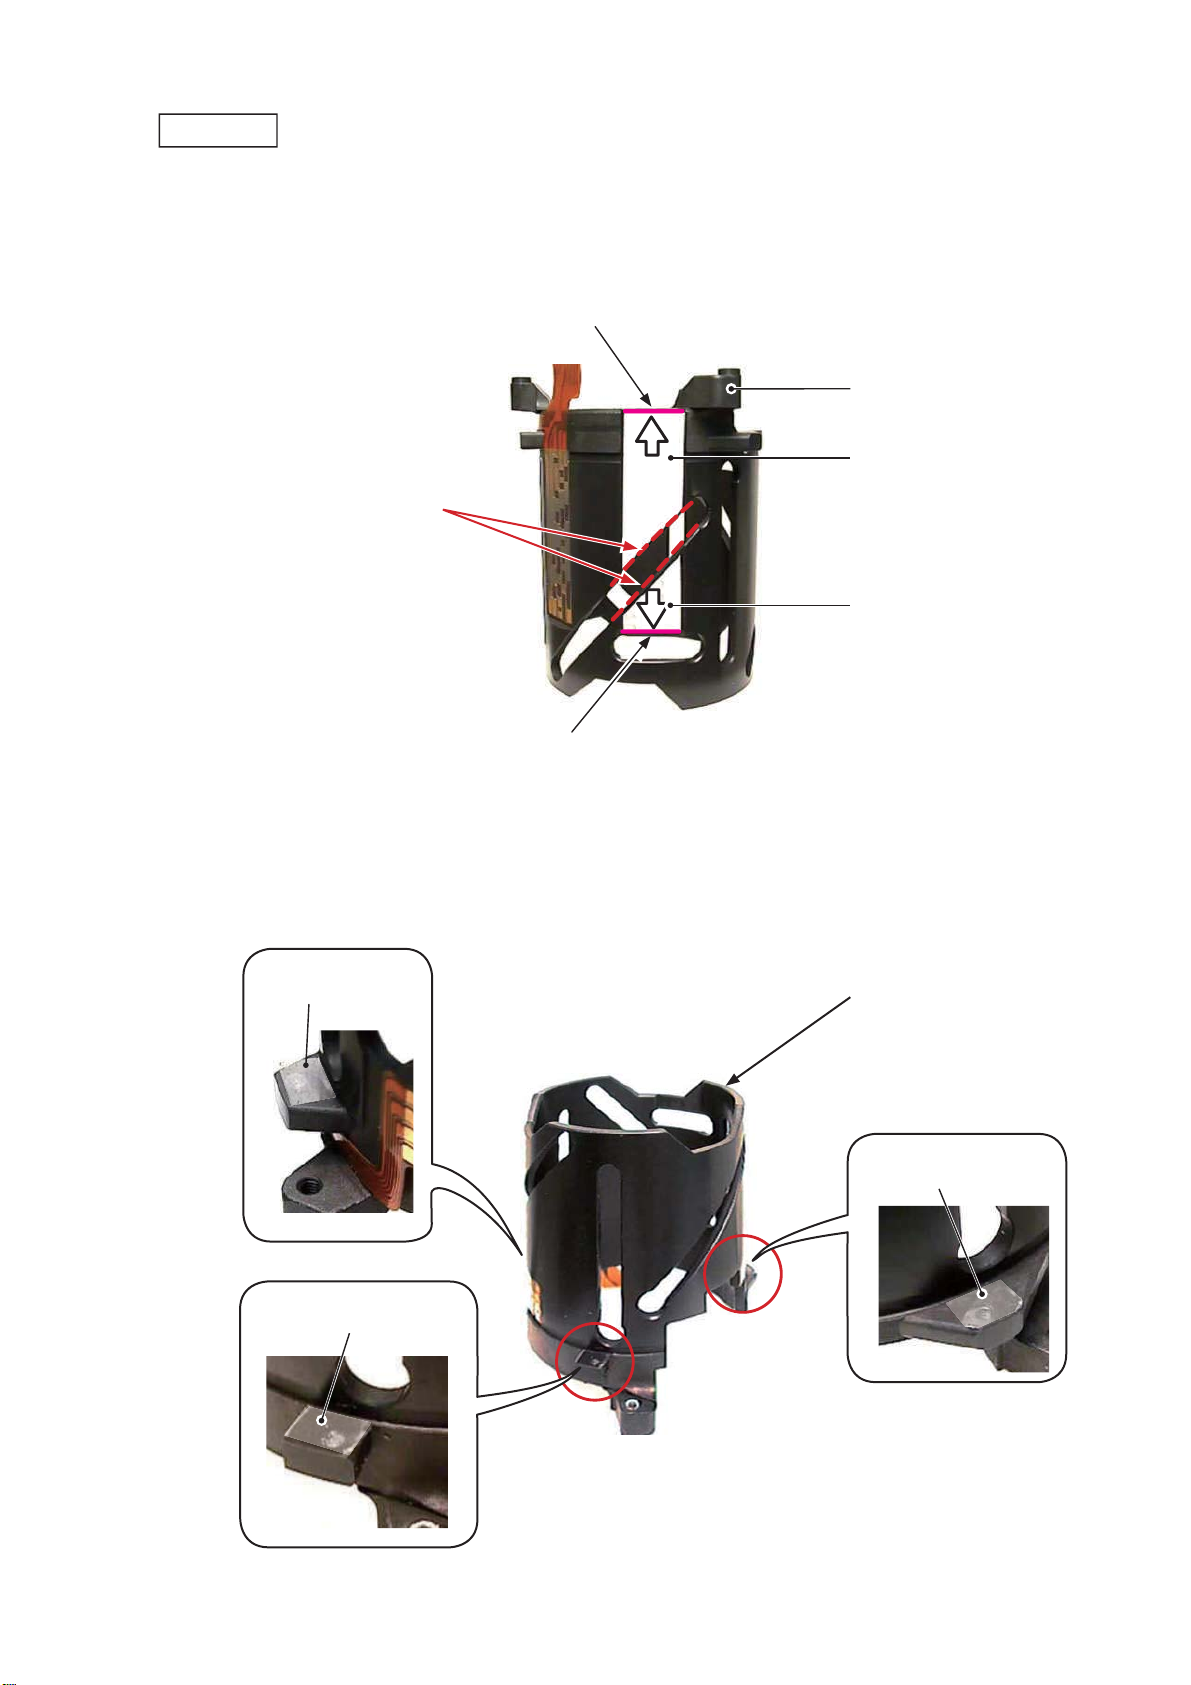
Tape
Place the two pieces of the double-stick tape (#149 and #150) on the fi xed tube (#50) based on the below
・
reference position each, and attach it by pressing in the direction of the arrow for positioning.
Reference position
#50
Caution:
When the tape is attached, it must
NOT cross the dot lines which show
the edges of the cam groove.
Reference position
Adhere the three pieces of the tape to cover the screw holes.
・
TA-0012
5×3.5
#150
#149
#50
TA-0012
5×3.5
TA-0012
5×3.5
- A2・AF-S DX 16-85/3.5-5.6G VR -
Page 25
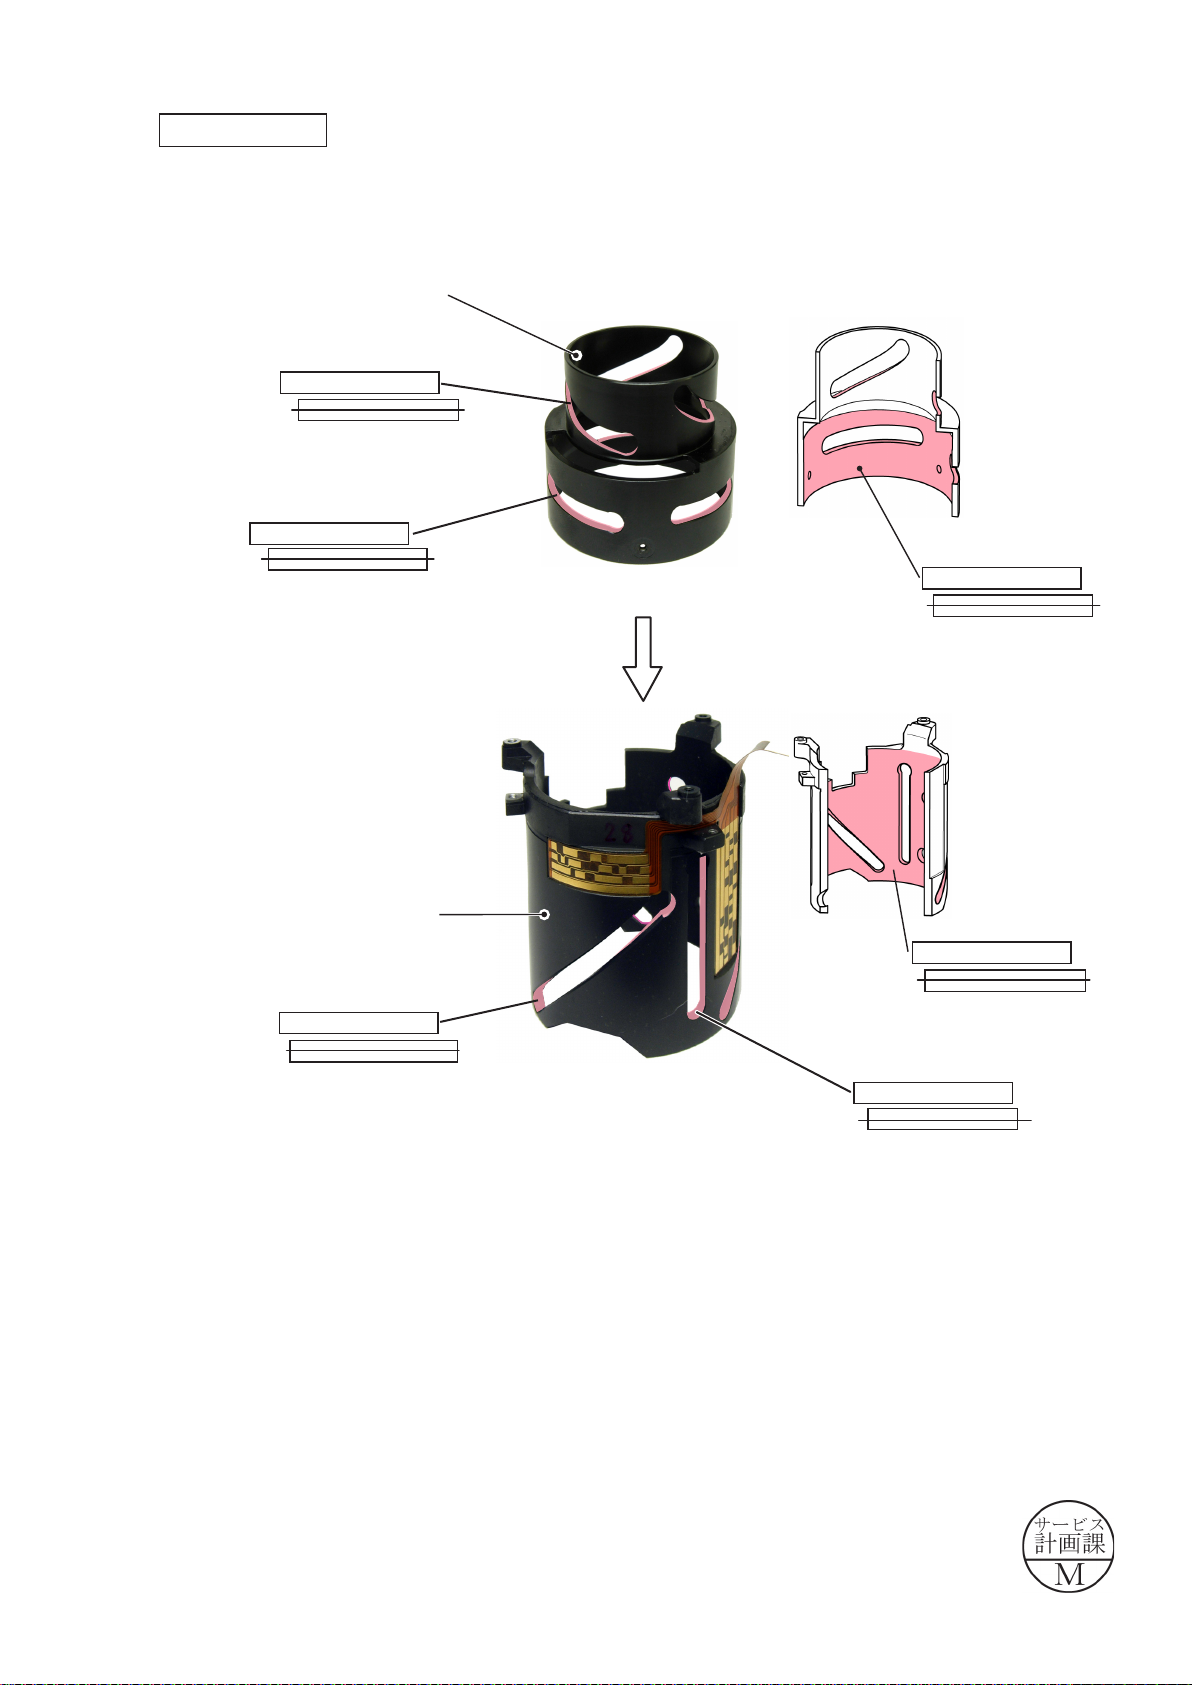
Fixed tube
INC
Assemble the 3-4 lens-G cam ring (#24) into the xed tube (#50).
・
#24
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall sliding surfaces of the
three cam grooves.
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall sliding surfaces of the
three cam grooves.
JAA80051-R.3741.A
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall surface of
the inside.
#50
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall sliding surfaces of the
three cam grooves.
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall surface sliding with [#24].
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall sliding surfaces of the
three lead grooves.
Changed page △× 6
- 3・AF-S DX 6-85/3.5-5.6G VR -
March�3�008�3�0083�008�008008
Page 26
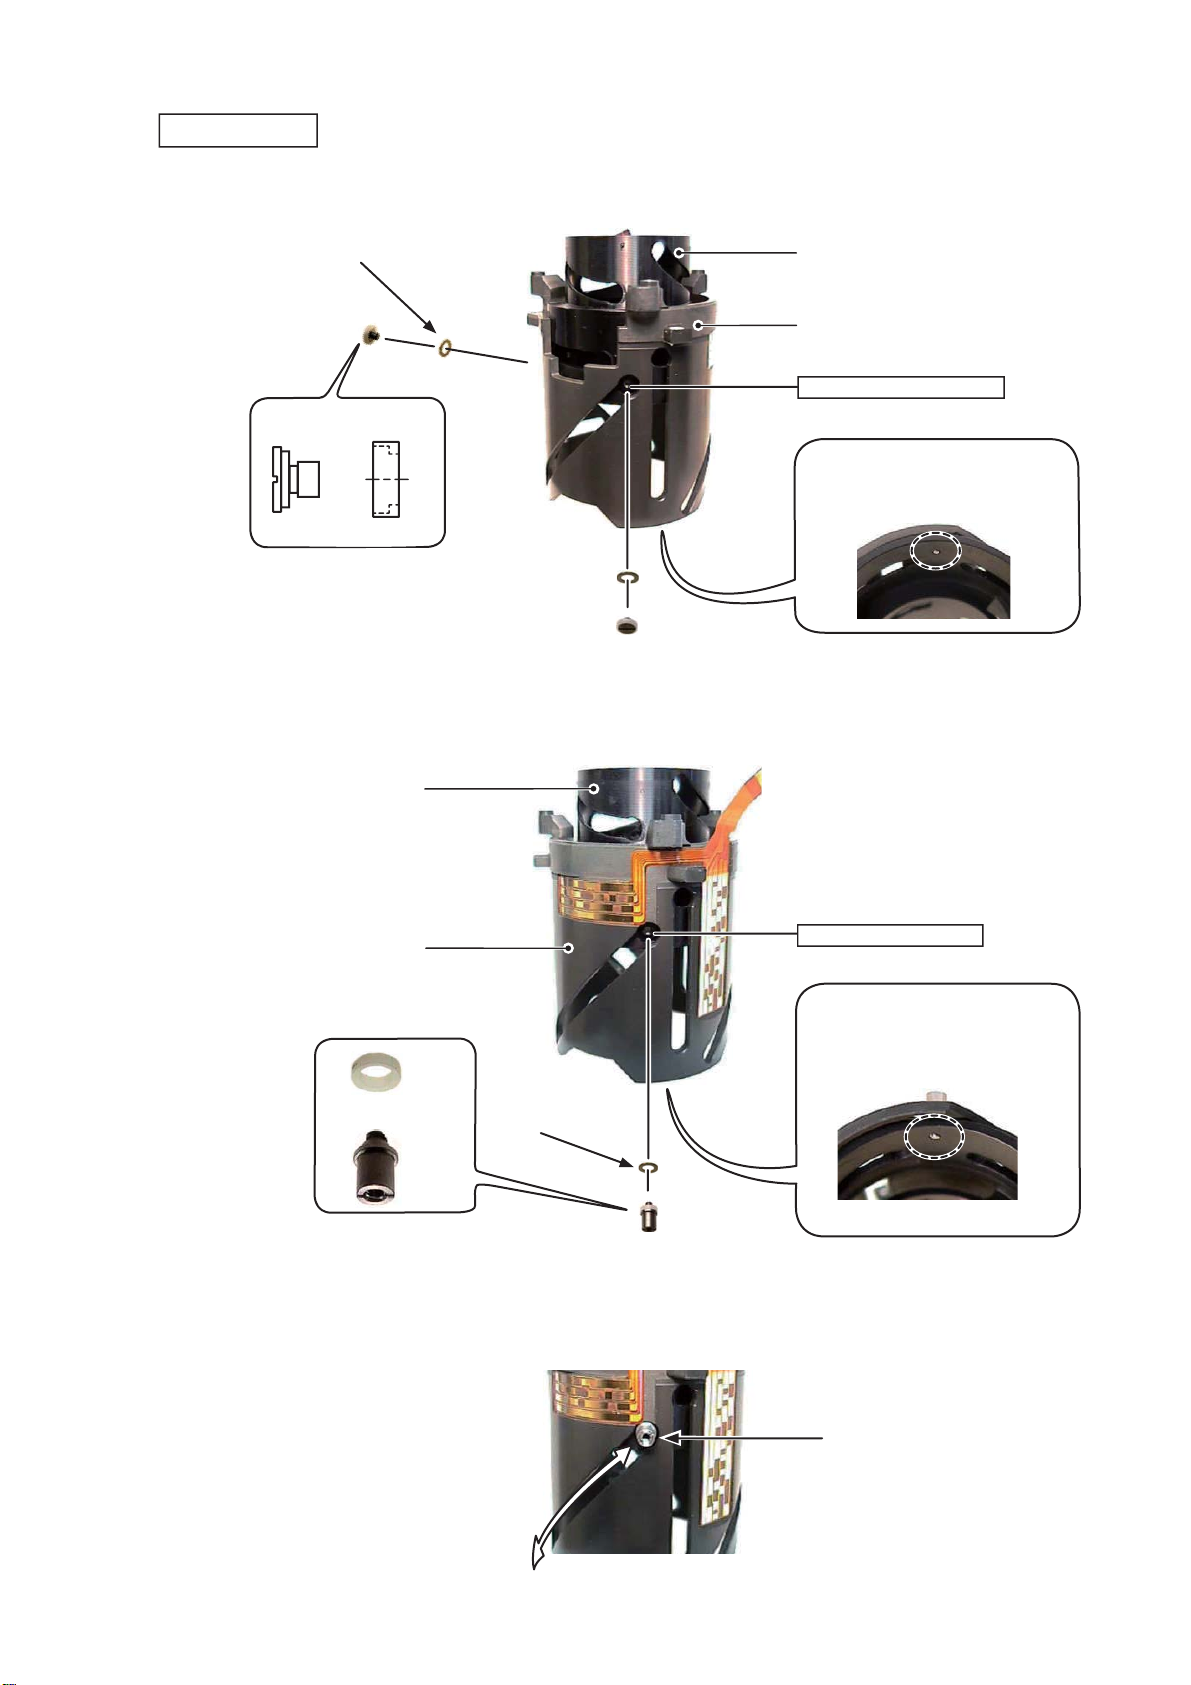
JAA80051-R.3741.A
INC
Roller unit
Mount the 3-4 lens-G cam ring (#24) on the fi xed tube (#50), and secure them with the two roller units (B83)
・
and two washers (#82).
#82×2
B83×2
#83×2
Attach the roller unit (B99) and washer (#82) to the 3-4 lens-G ring (#24).
・
#84×2
#24
#24
#50
Adhesive: Lockend (R)
Screw hole ×2
If the adhesive of [#24] is
squeezed out to the inside, wipe
it out.
#50
#94
#82
#99
Check the operations by sliding the roller unit (B99).
・
Adhesive: Lockend (R)
Screw hole
If the adhesive of [#24] is
squeezed out to the inside, wipe
it out.
B99
B99
- A4・AF-S DX 16-85/3.5-5.6G VR -
Page 27
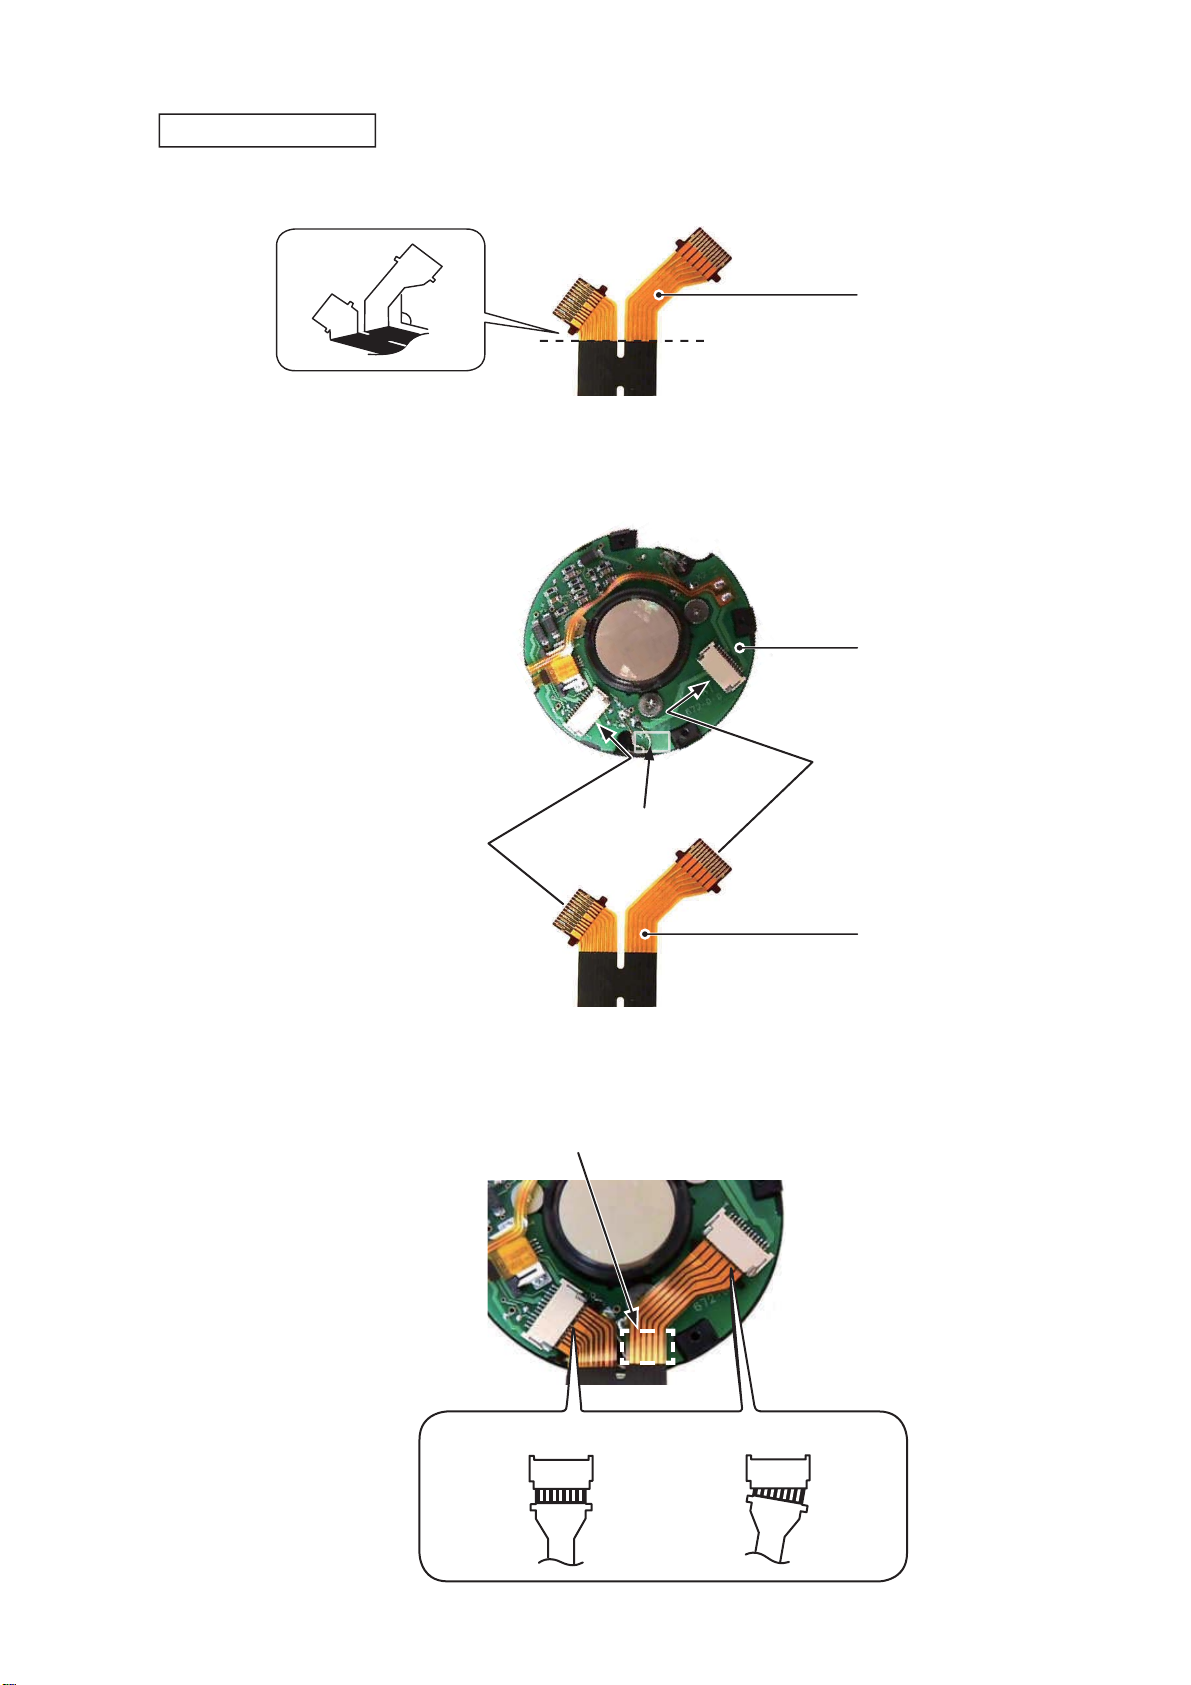
VR unit-assembly
INC
Make a valley-fold along the dotted line of the connection-FPC (#1108).
・
JAA80051-R.3741.A
90°
Valley-fold
Peel off the backing paper of the double-stick tape.
・
Connect the connection-FPC (#1108) to the connector of VR unit-assembly (B2308) in numeric order from
・
to②.
①
Double-stick tape
②
①
#1108
B2308
#1108
Push the double-stick tape from above with the fi ngers to fi xate the connection-FPC (#1108)
・
Double-stick tape
Insert FPC all the way
seated in.
Do NOT insert FPC sideways.
- A5・AF-S DX 16-85/3.5-5.6G VR -
Page 28
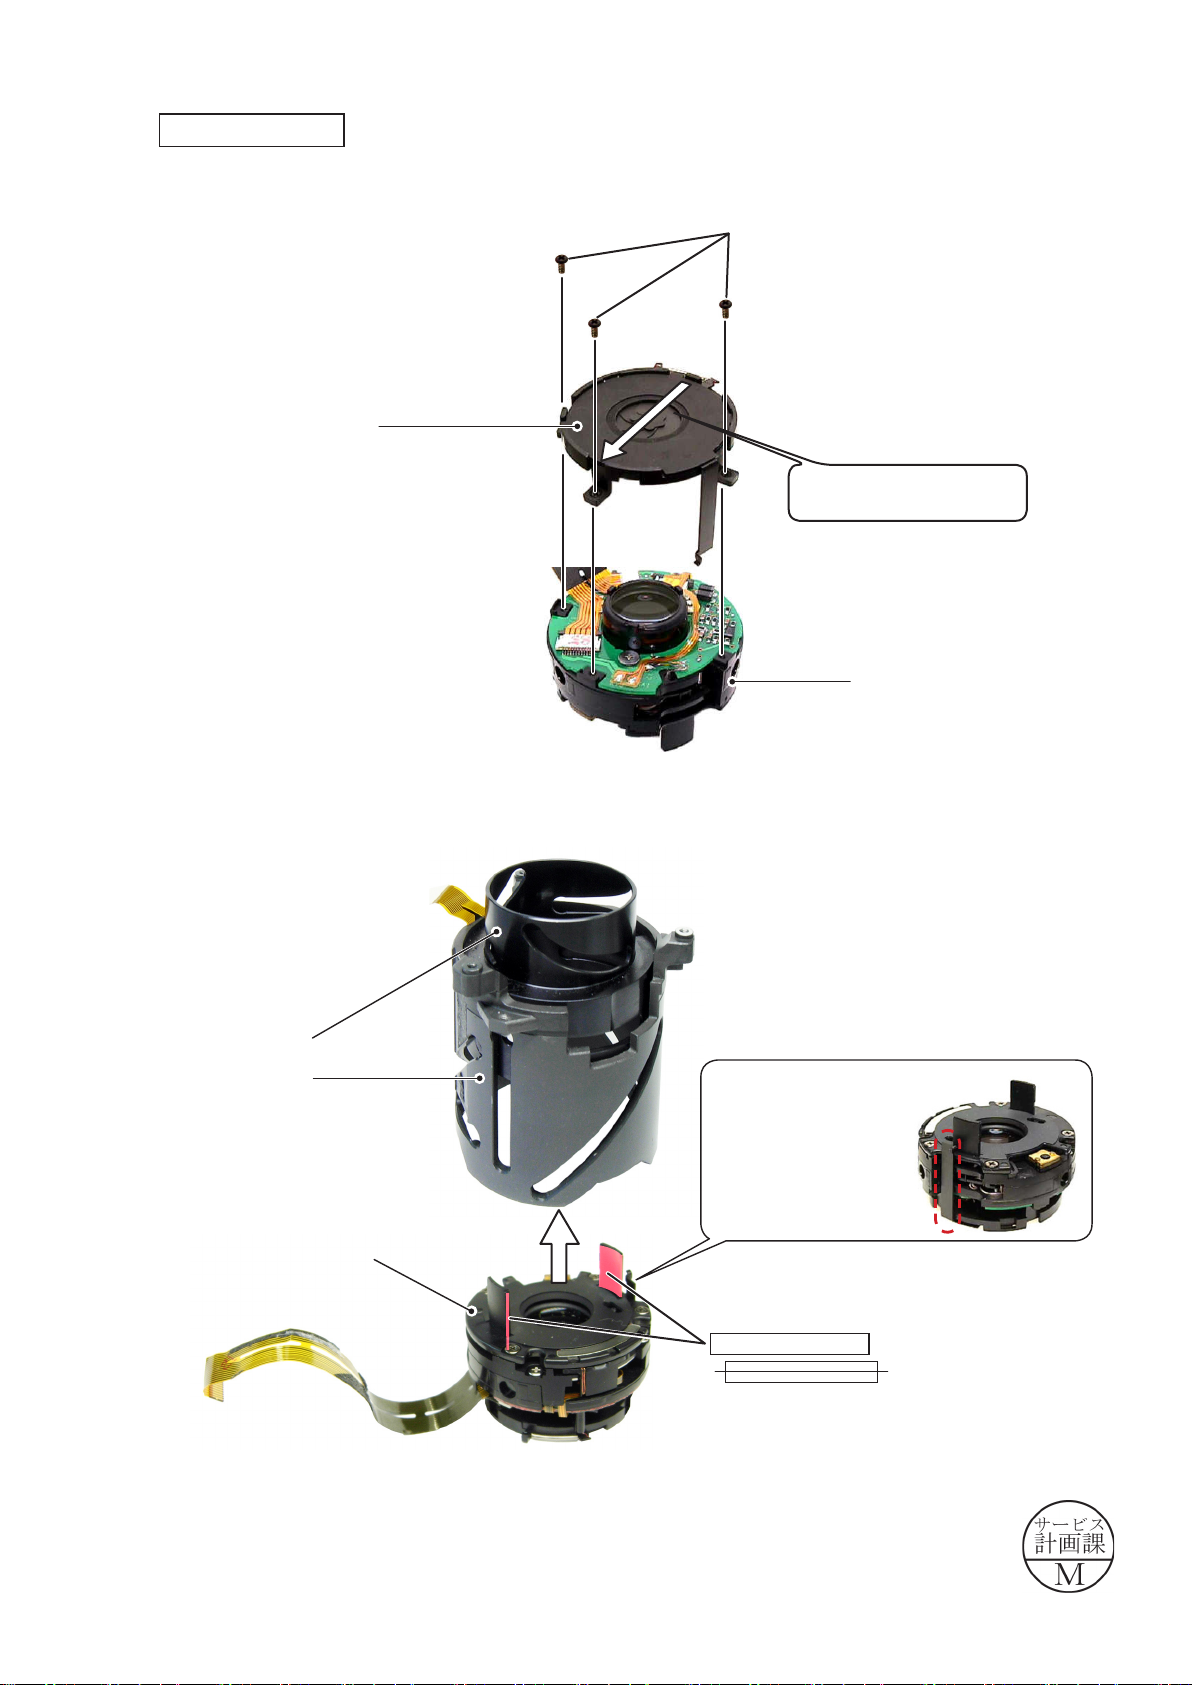
JAA80051-R.3741.A
INC
Aperture unit
Position the aperture unit (B34) in the direction of the arrow, and tighten the three screws (#56) in numeric
・
order ①, ②, and ③.
#56×3
②
③
①
B34
Direction of positioning
Assemble VR unit (B2308) into the 3-4 lens-G cam ring (#24).
・
#48
#24
B2308
B2308
Be careful NOT to
hold the lever when
assembling, in order to
prevent deformation.
Changed page △× 1
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the two lateral and inner
surfaces of the protrusions.
- 6・AF-S DX 6-85/3.5-5.6G VR -
March�3�008�3�0083�008�008008
Page 29
JAA80051-R.3741.A
INC
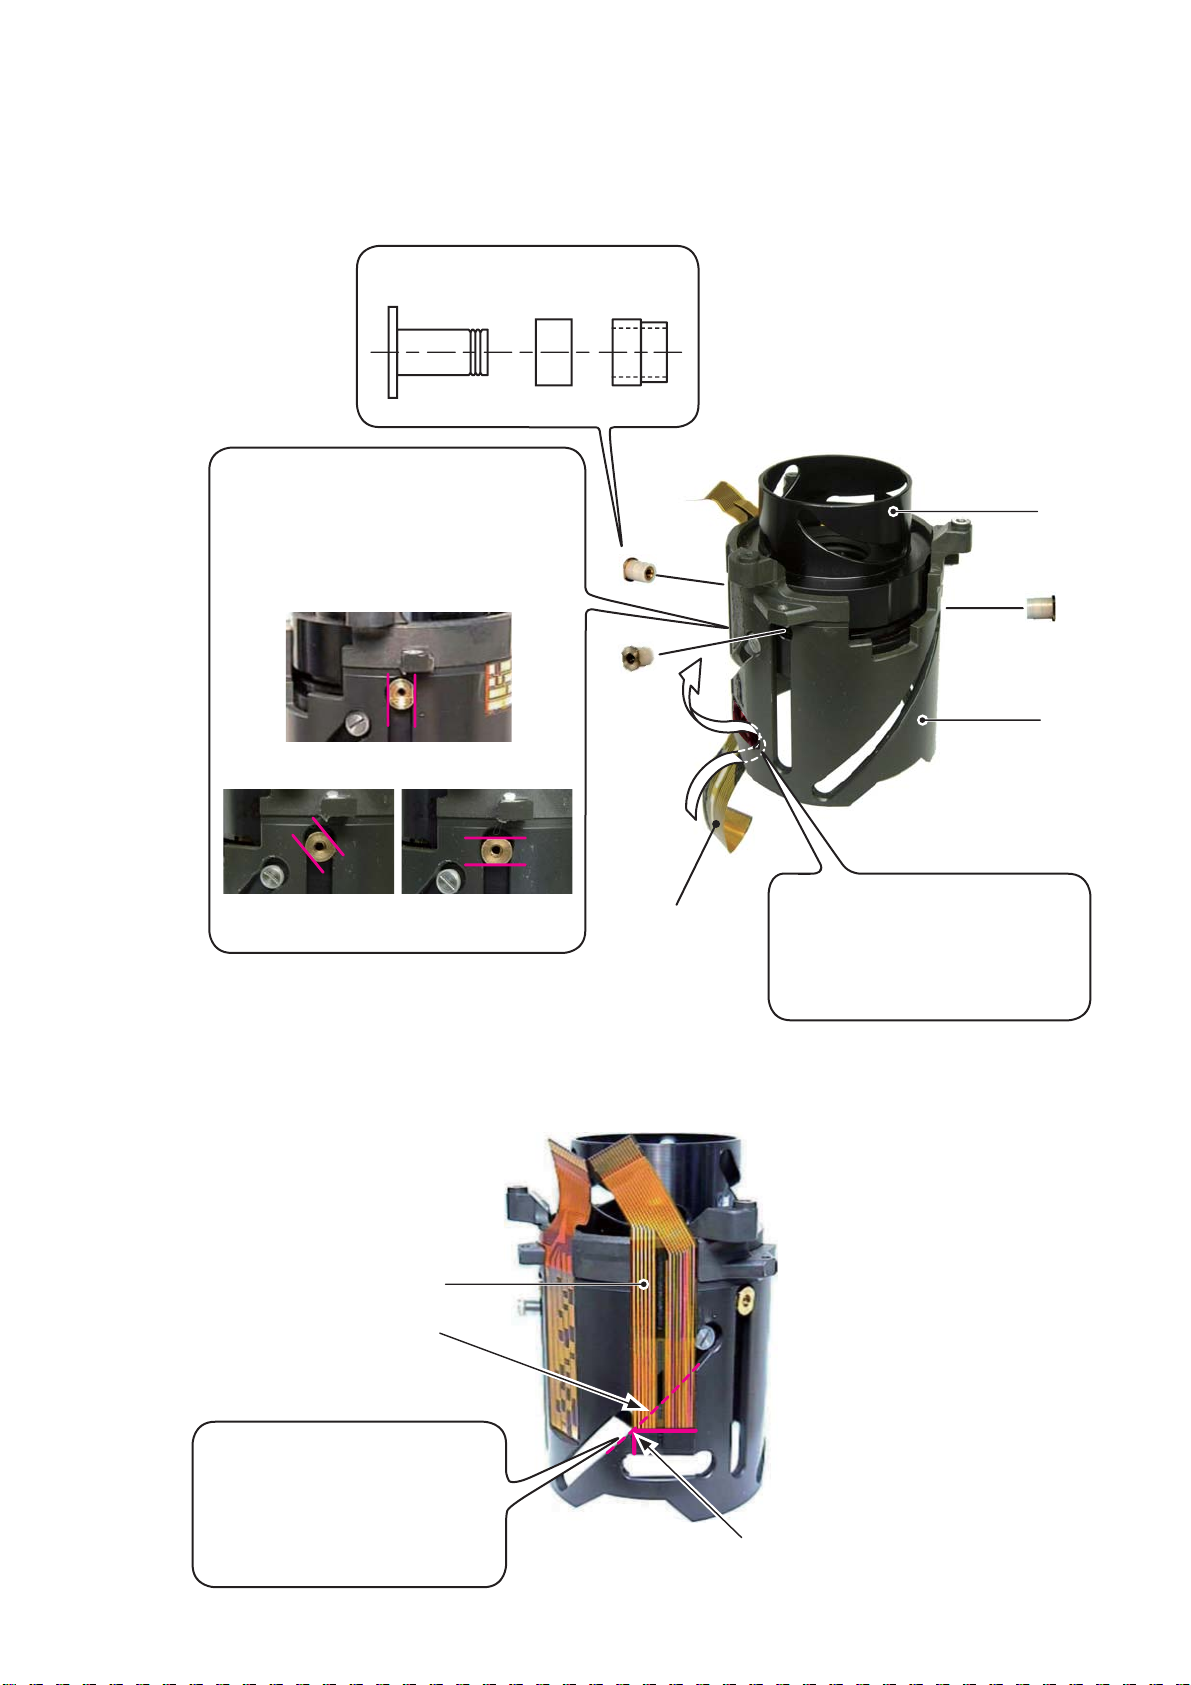
Assemble the fi xed tube (#50), 3-4 lens-G cam ring (#24), and VR unit-assembly (B2308) together by using
・
the three roller units (B68).
#68×3
The head of the roller unit (B68) must be
positioned against the lead groove as below.
GOOD
<
<
BAD
>
>
#147×3
#148×3
#24
B68×3
#50
Through this hole, pass the
#1008
Peel off the backing papers of the double-stick tapes (#149 and #150) and attach the connection-FPC
・
connection-FPC (#1008) from
the inside of the fi xed tube (#50)
toward the outside.
(#1008).
#1008
Edge line of the cam groove
Attach the FPC based on the refer-
ence position and dot line (edge of
cam groove), being careful of the
corner as shown in the right picture.
Reference position
- A7・AF-S DX 16-85/3.5-5.6G VR -
Page 30
JAA80051-R.3741.A
INC
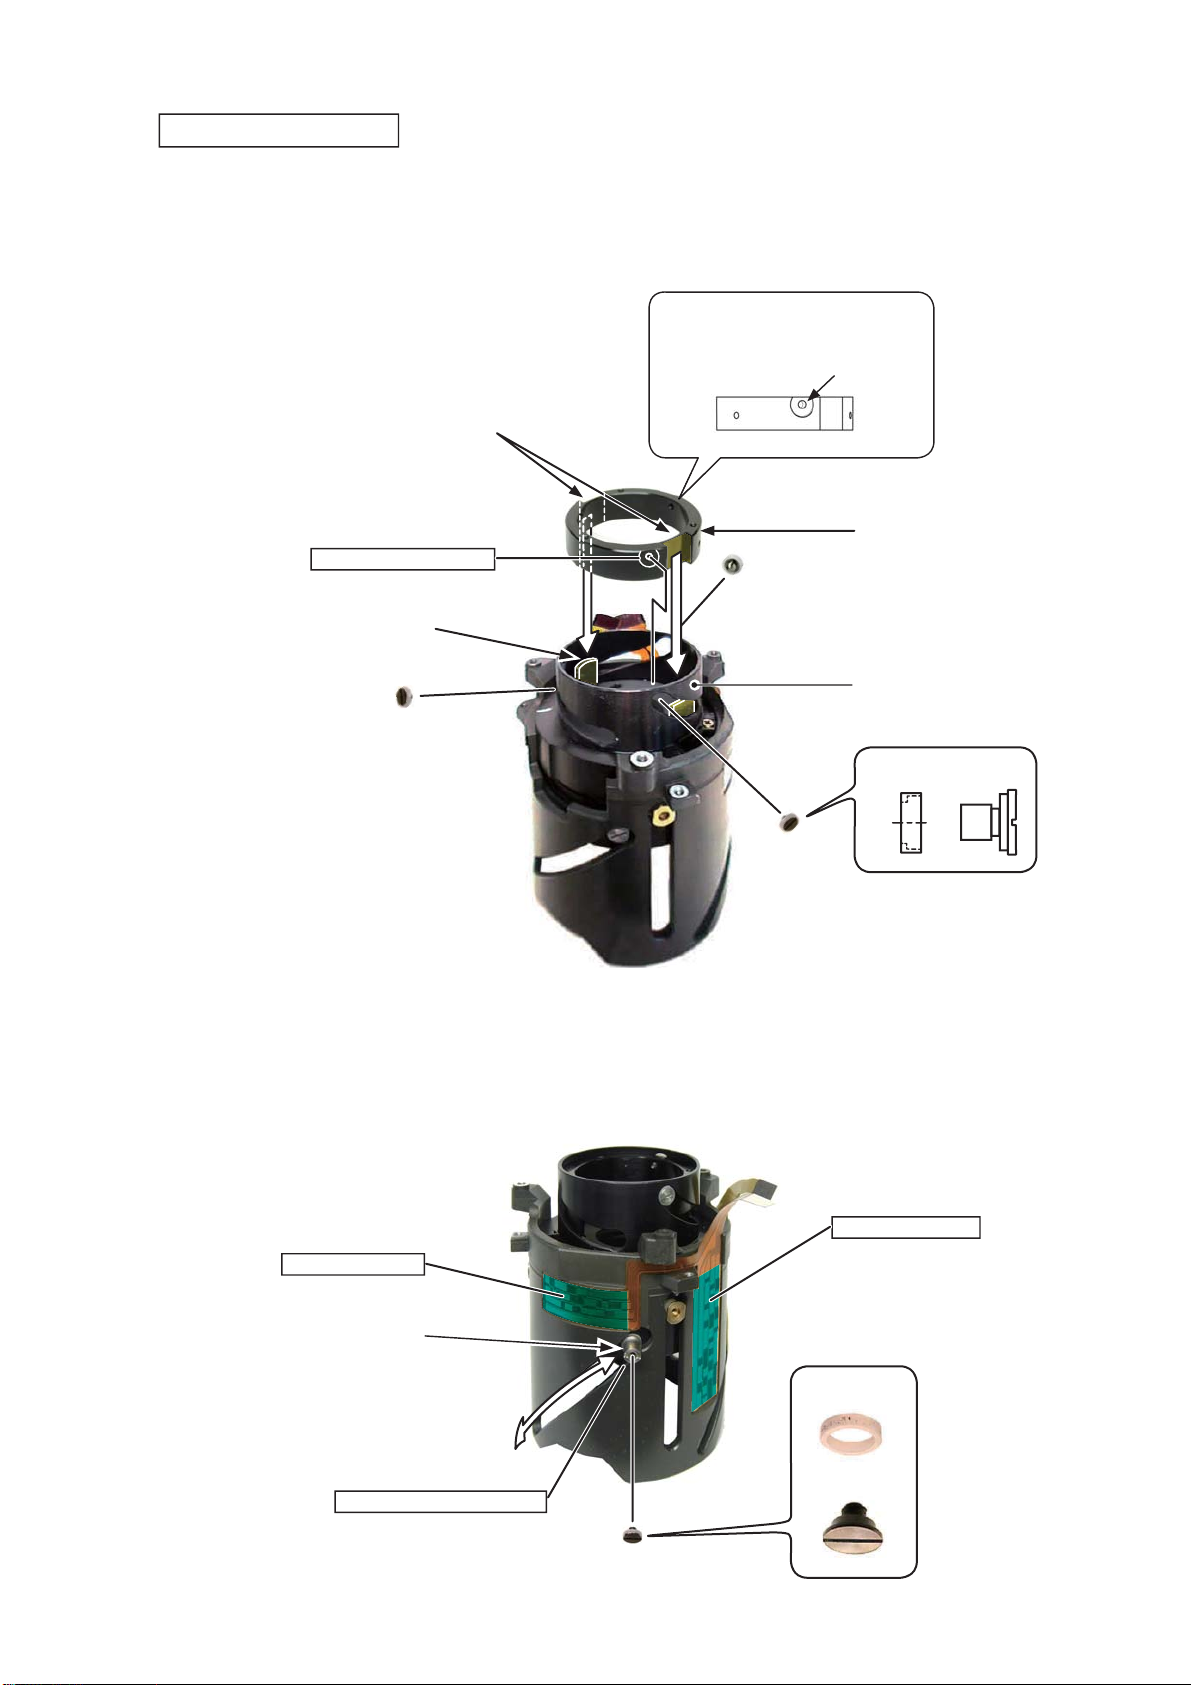
4th lens-G sliding ring
Mount the 4th lens-G sliding ring (#48) by fi tting its two cutouts with the two protrusions of VR unit.
・
Attach the three roller units (B81) to the 4th lens-G sliding ring (#48) through the cam groove of the 3-4
・
lens-G cam ring (#24) and fasten them.
Be careful of up/downward
direction for mounting.
Screw hole
Cutout×2
#48
Adhesive: Lockend (B
Screw hole ×3
Protrusion×2 of VR unit
)
Attach the roller unit (B102) to the roller unit (B99) and fasten it.
・
Check operations by sliding the roller unit (B99).
・
Grease: PL-22SEL
Pattern surface
B81×3
#24
#84×3
Grease: PL-22SEL
Pattern surface
#81×3
B99
Adhesive: Lockend (R
Screw hole
- A8・AF-S DX 16-85/3.5-5.6G VR -
#103
#102
)
B102
Page 31
JAA80051-R.3741.A
INC
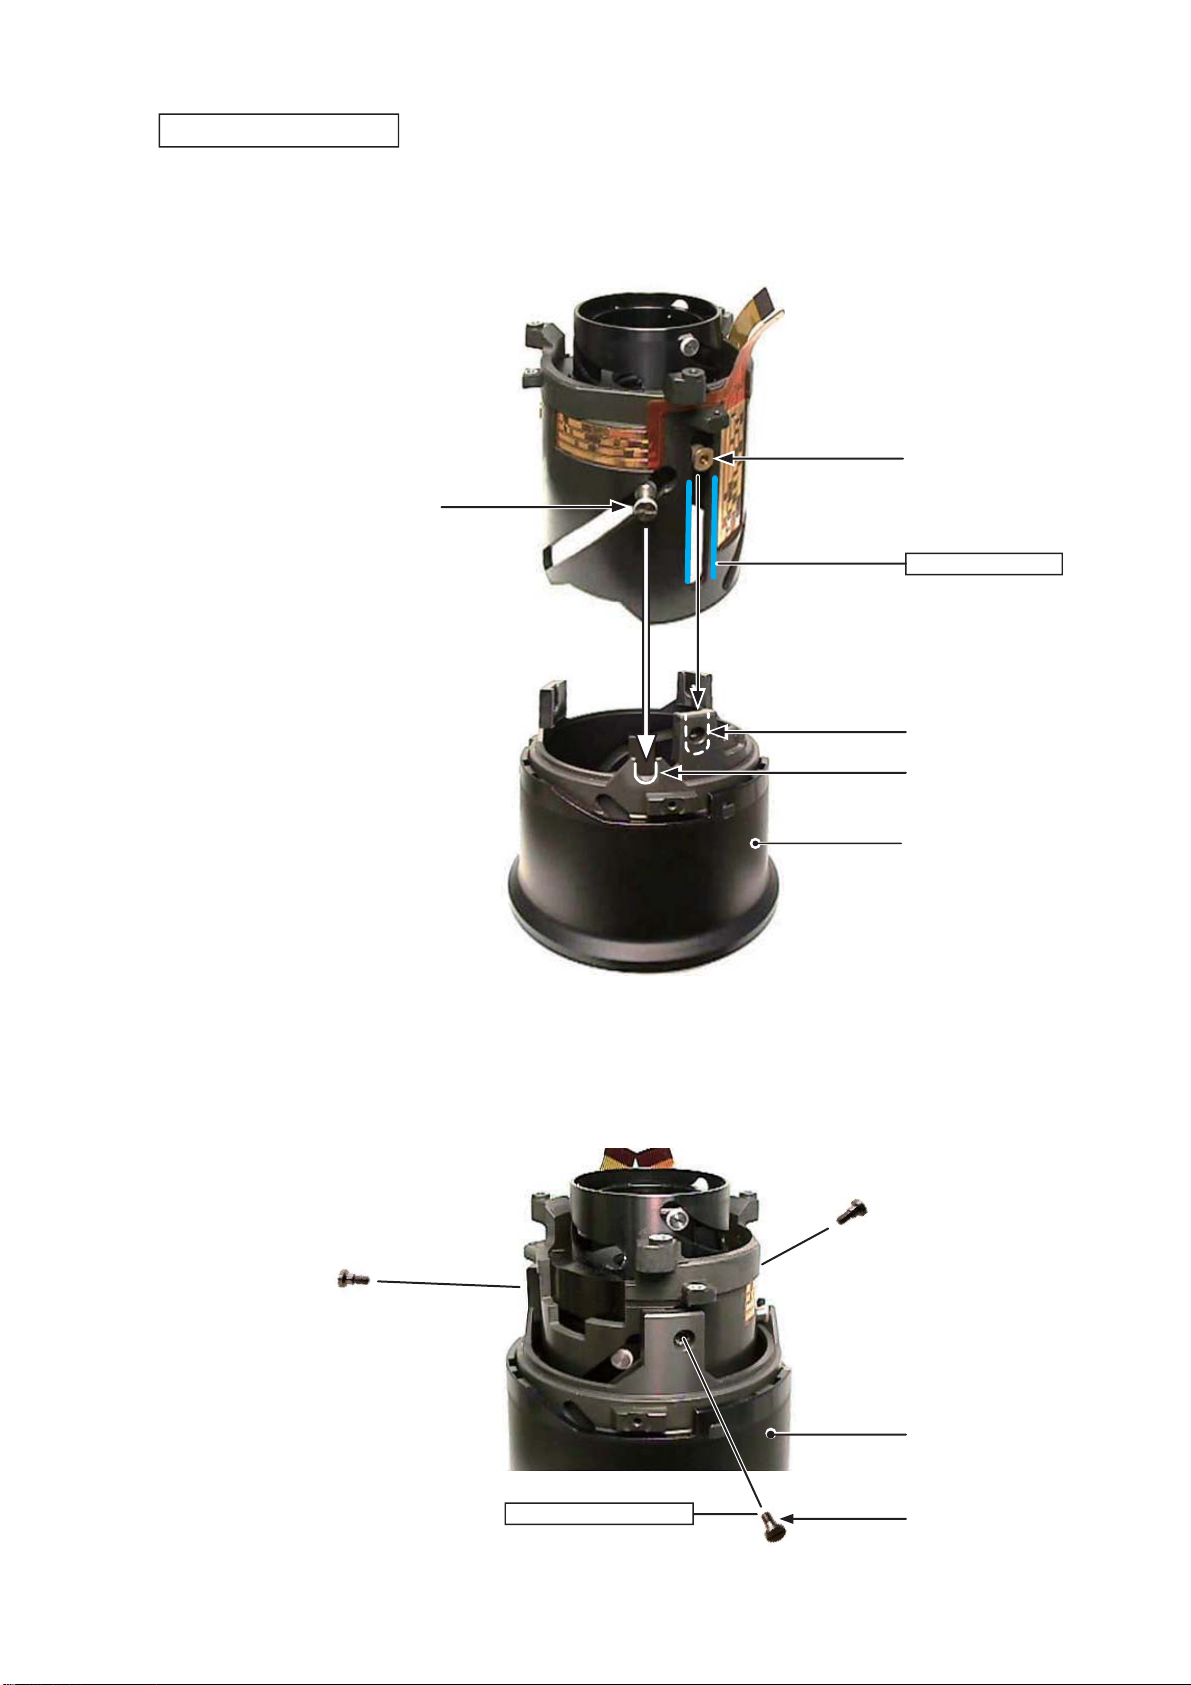
2nd lens-G straight ring
Align the position of the roller unit (B99) with "U-groove" of the 2nd lens-G straight ring unit (B52).
・
Align the three roller units (B68) with three cutouts of the 2nd lens-G straight ring unit (B52), and make
・
assembly.
B68
B99
Grease: GP-1RS
Apply to the six surfaces sliding
with [B52].
Attach the three screws (#67) to the 2nd lens-G straight ring unit (B52) and fasten them.
・
Cutout×3
U-groove
B52
Adhesive: Lockend (R
Apply to the screw head ×3
- A9・AF-S DX 16-85/3.5-5.6G VR -
)
B52
#67×3
Page 32
JAA80051-R.3741.A
INC
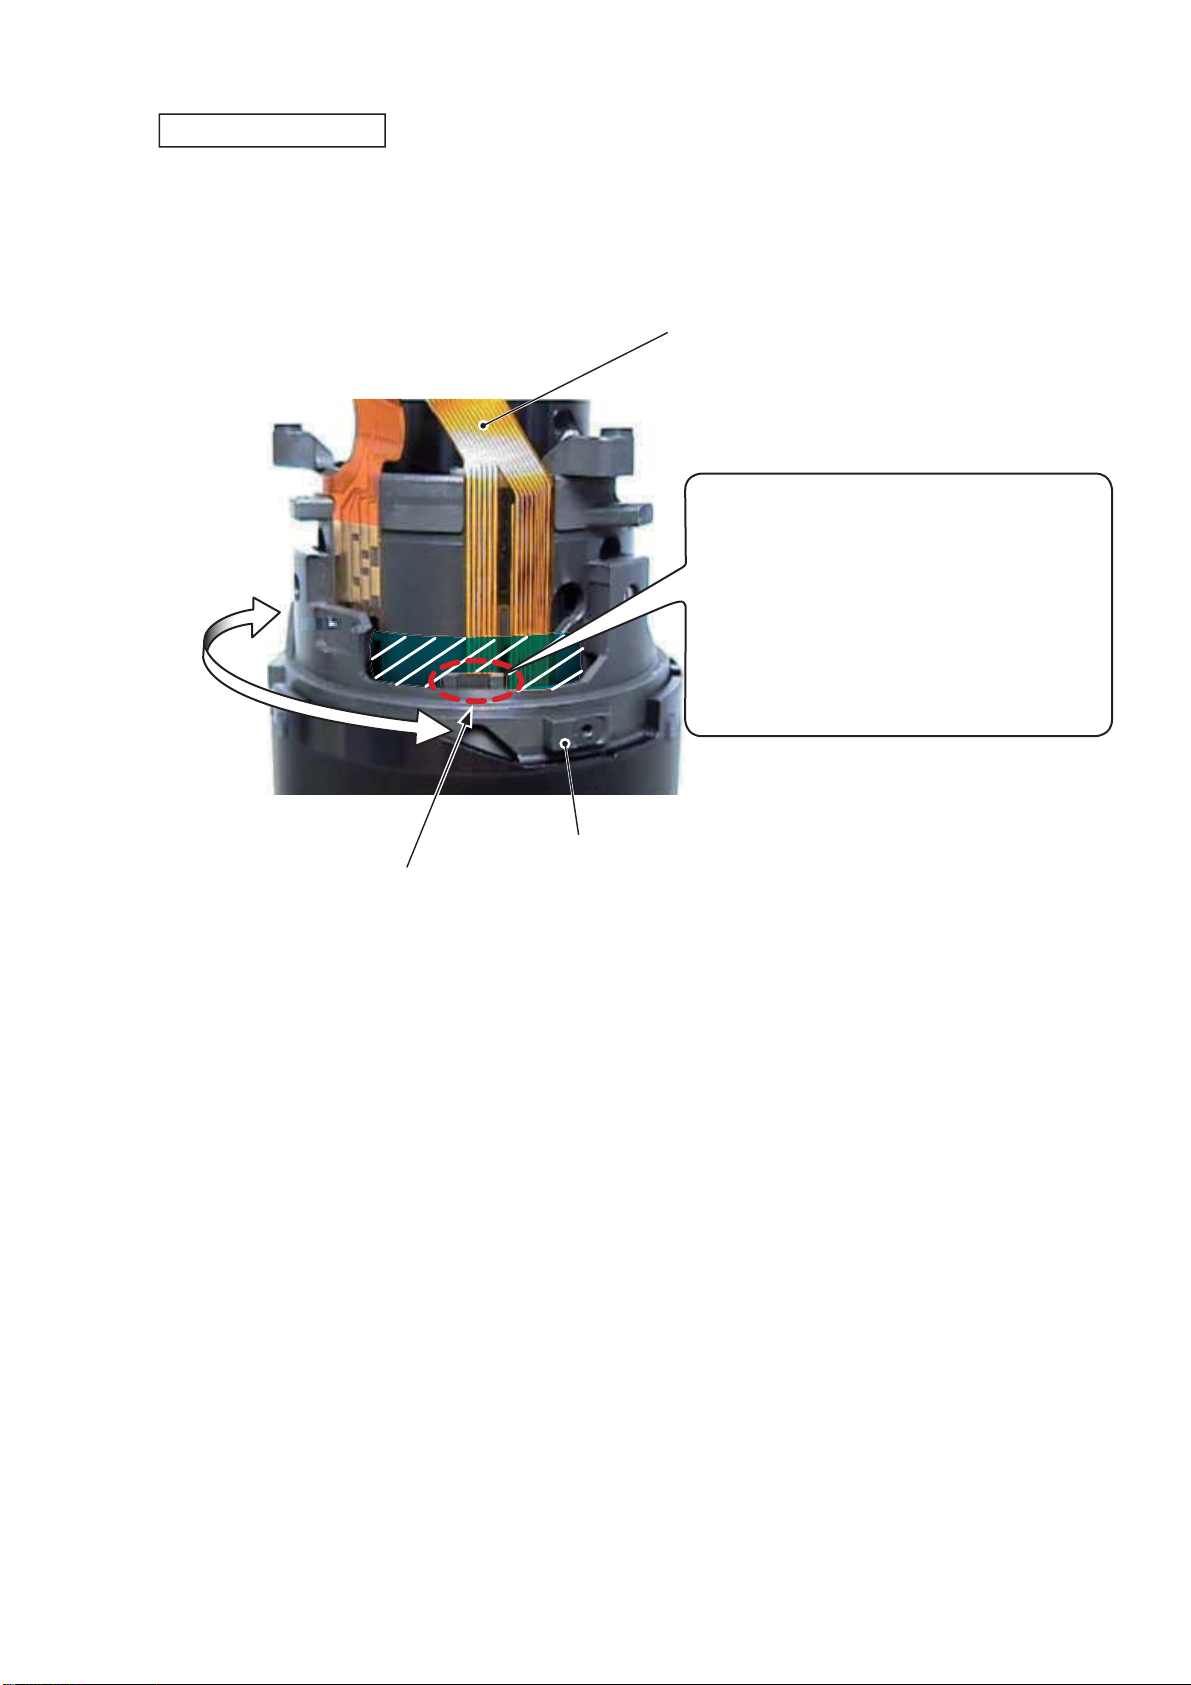
Zoom operation check
Rotate the 2nd lens-G turning-ring (#53), and check operations of the 2nd lens-G straight ring unit (B52).
・
#1008
During rotating the 2nd lens-G turning-ring
・
(#53), the lever section of the 2nd lens-G cam
ring (#25) must be positioned in the shaded por-
tion.
If the lever gets stuck with the connection-FPC
・
Lever section of [#25]
(#1008), change the double-stick tape and re-
attach the connection-FPC.
#53
- A10・AF-S DX 16-85/3.5-5.6G VR -
Page 33
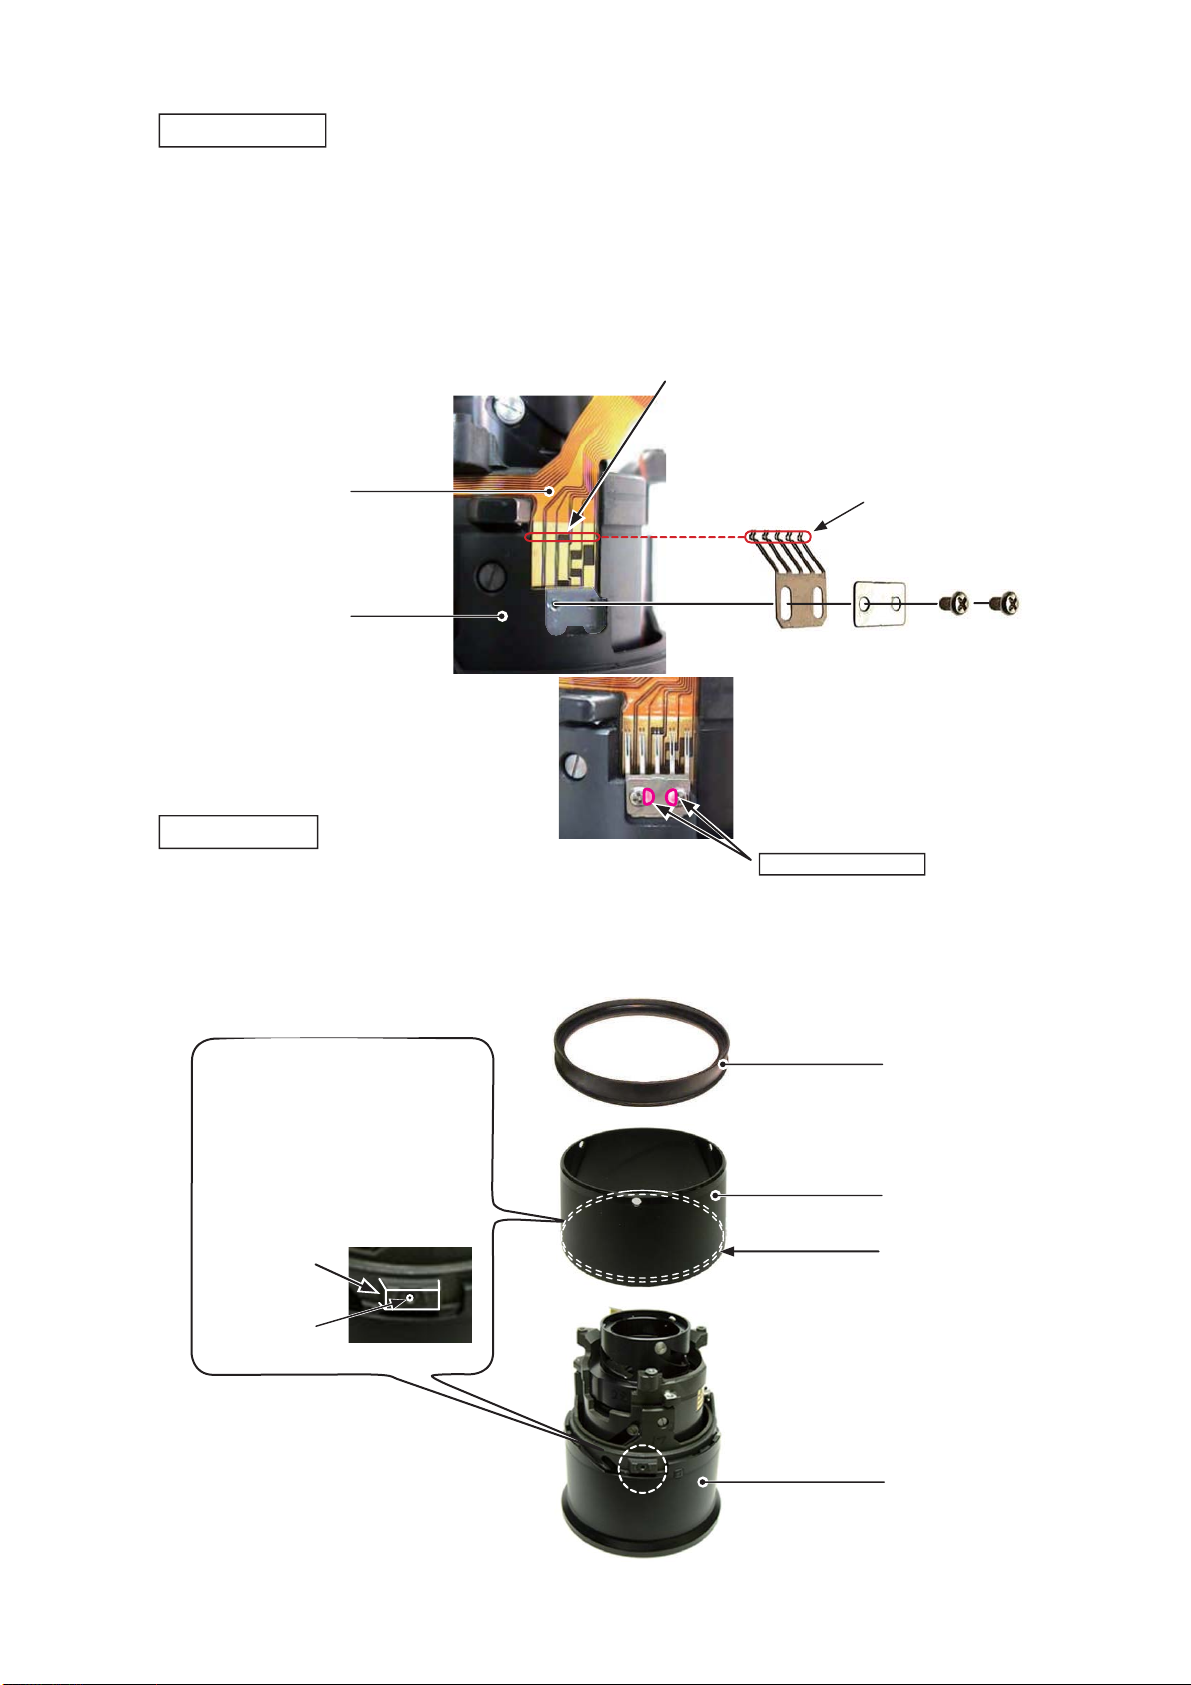
JAA80051-R.3741.A
INC
Zoom brush
Set the zoom ring to WIDE.
・
Attach the zoom brush (#104) and reinforcing plate (#106) to the 2nd lens-G straight ring unit (B52), and
・
secure them with the two screws (#109).
Activate zooming. Check the contacting condition on the overall pattern of the encoder-FPC (#1008) and
・
the start position of the brush.
After checking the brush start position, apply the adhesive to the head of the two screws (#109) and fasten
・
them.
#1008
B52
Brush attaching (start) position at WIDE-end
Set "R" section which is the head of the zoom brush
at the start position.
"R" section
#104
#106 #109×2
Caution:
Do NOT deform the brush.
・
Do NOT use a deformed brush.
・
Cover ring unit
Mount the cover ring unit (B36) with the holes facing upwards by fi tting in the three screw holes of the
・
#109×2
Adhesive: Screwlock
2nd lens-G straight ring unit (B52).
Mount the support ring unit (B101).
・
When [B36] is mounted, the three
convex portions of the 2nd lens-G
straight ring must not get stuck
with the fi ne tape (#78) of the cover
ring unit
Convex
portion ×3
Screw hole ×3
B101
B36
#78
B52
- A11・AF-S DX 16-85/3.5-5.6G VR -
Page 34
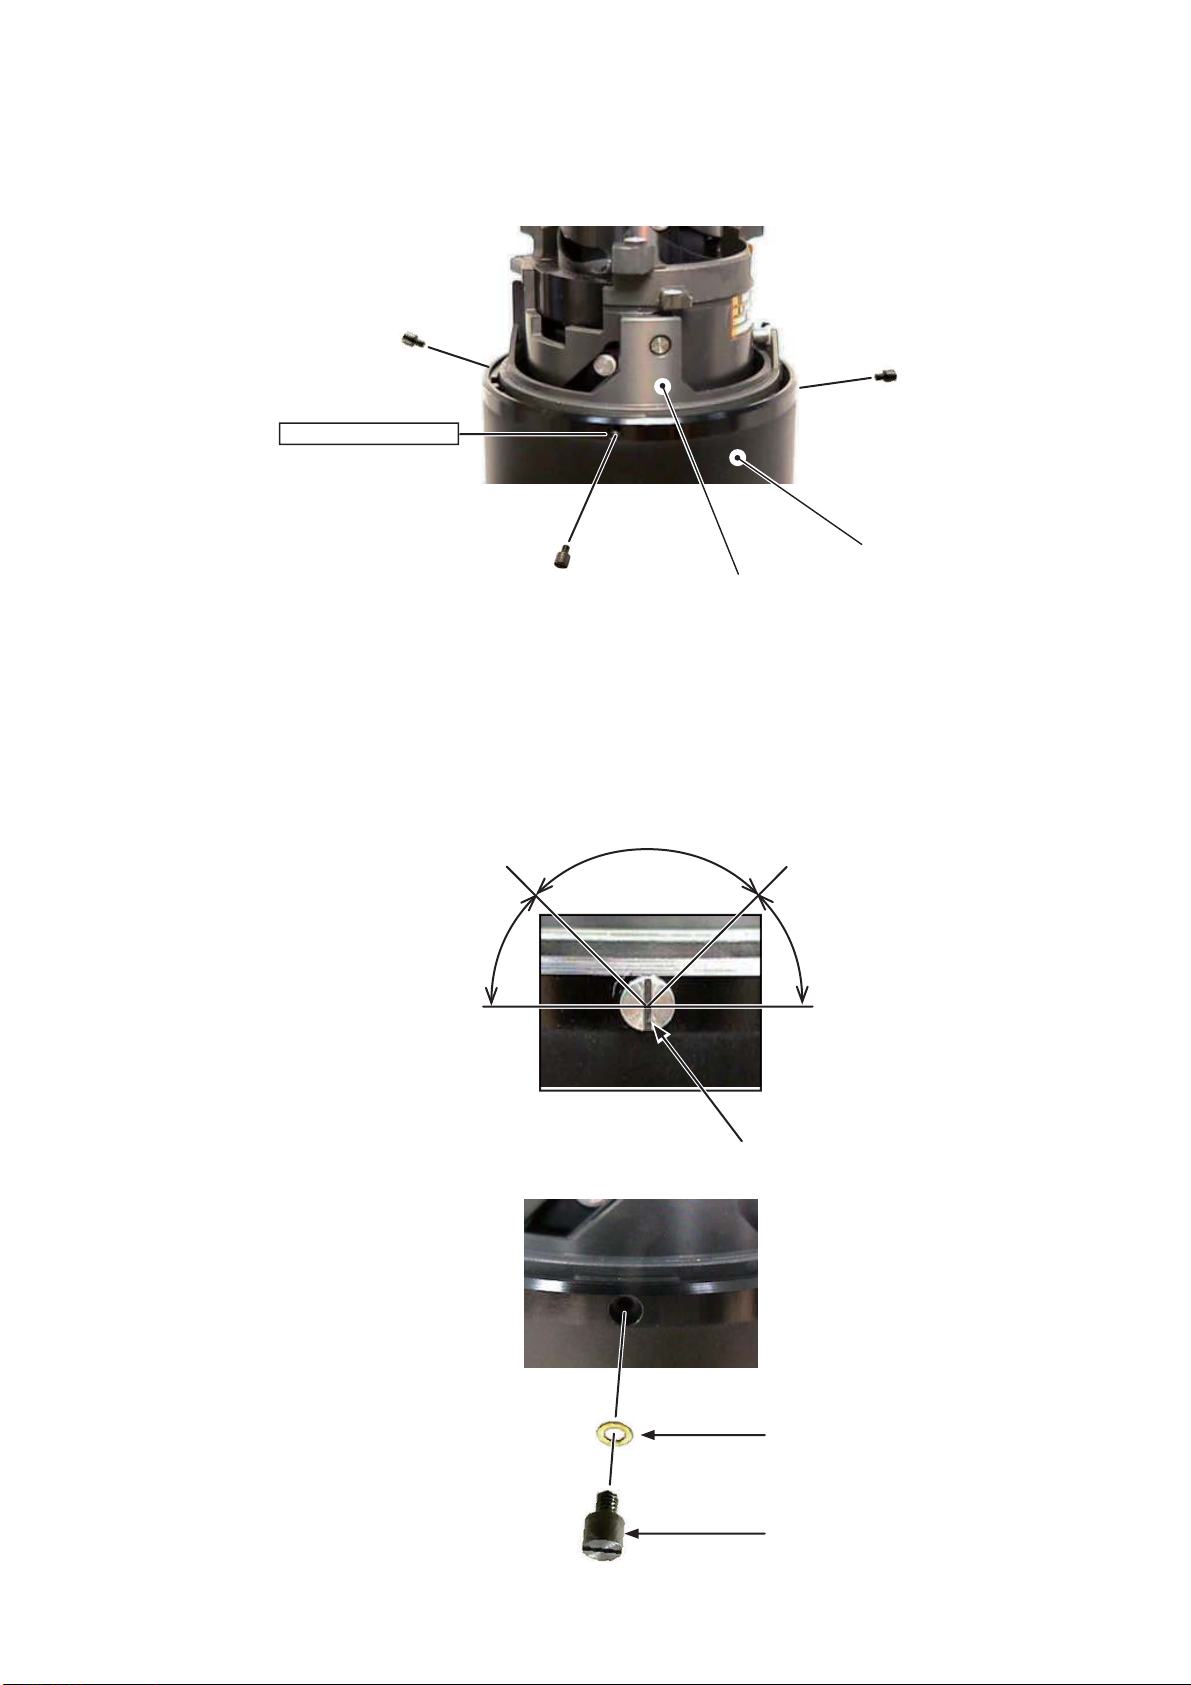
JAA80051-R.3741.A
INC
Tighten the three screws (#110) and fi x the cover ring unit (B36) and 2nd lens-G straight ring unit (B52).
・
Adhesive: Lockend (B
Screw hole ×3
Confi rm that after tightening the screw (#110), the slot’s angle is within the appropriate range.
・
If the slot’s angle is wihin the adjustable range, adjust it by tightening the screw (#110) and washer (#107)
・
)
B36
#110×3
B52
together so as that it becomes in the appropriate range.
Appropriate range (45°
Adjustable range
(135°~180°)
180°
~
135°)
Adjustable range
(0°~45°)
0°
Slot
#107
#110
- A12・AF-S DX 16-85/3.5-5.6G VR -
Page 35
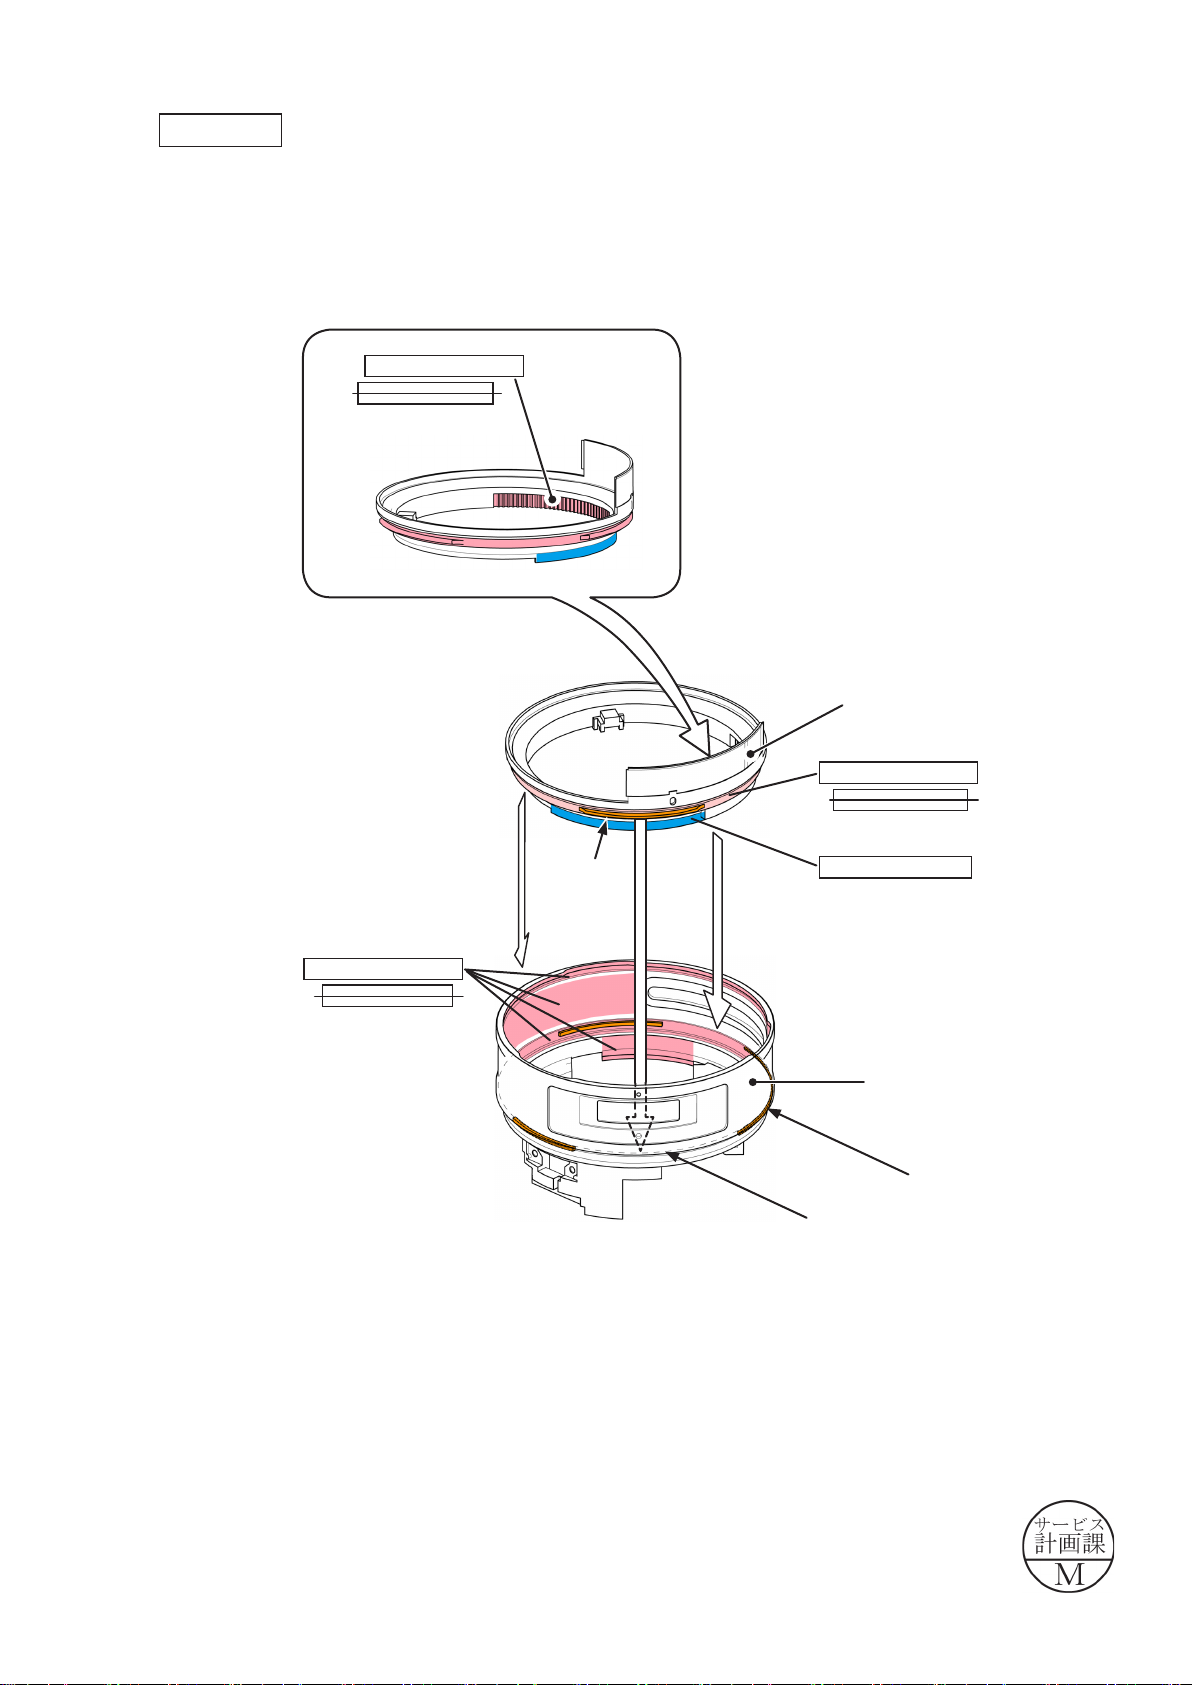
JAA80051-R.3741.A
INC
Gear unit
Mount the gear unit (B40) by tting the three protrusions with the three cutouts of the xed tube (#55).
・
Turn the gear unit (B40) from side to side, so that it is xed in the xed ring (#55).
・
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the surface sliding
with gear unit.
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the surfaces sliding
with [B40] and [B27].
Protrusion×3
B40
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the surface sliding with [#55].
Grease: PL-22SEL
Apply to the magnetic tape.
#55
Protrusion×3
Cutout×3
Changed page △× 3
- 3・AF-S DX 6-85/3.5-5.6G VR -
March�3�008�3�0083�008�008008
Page 36
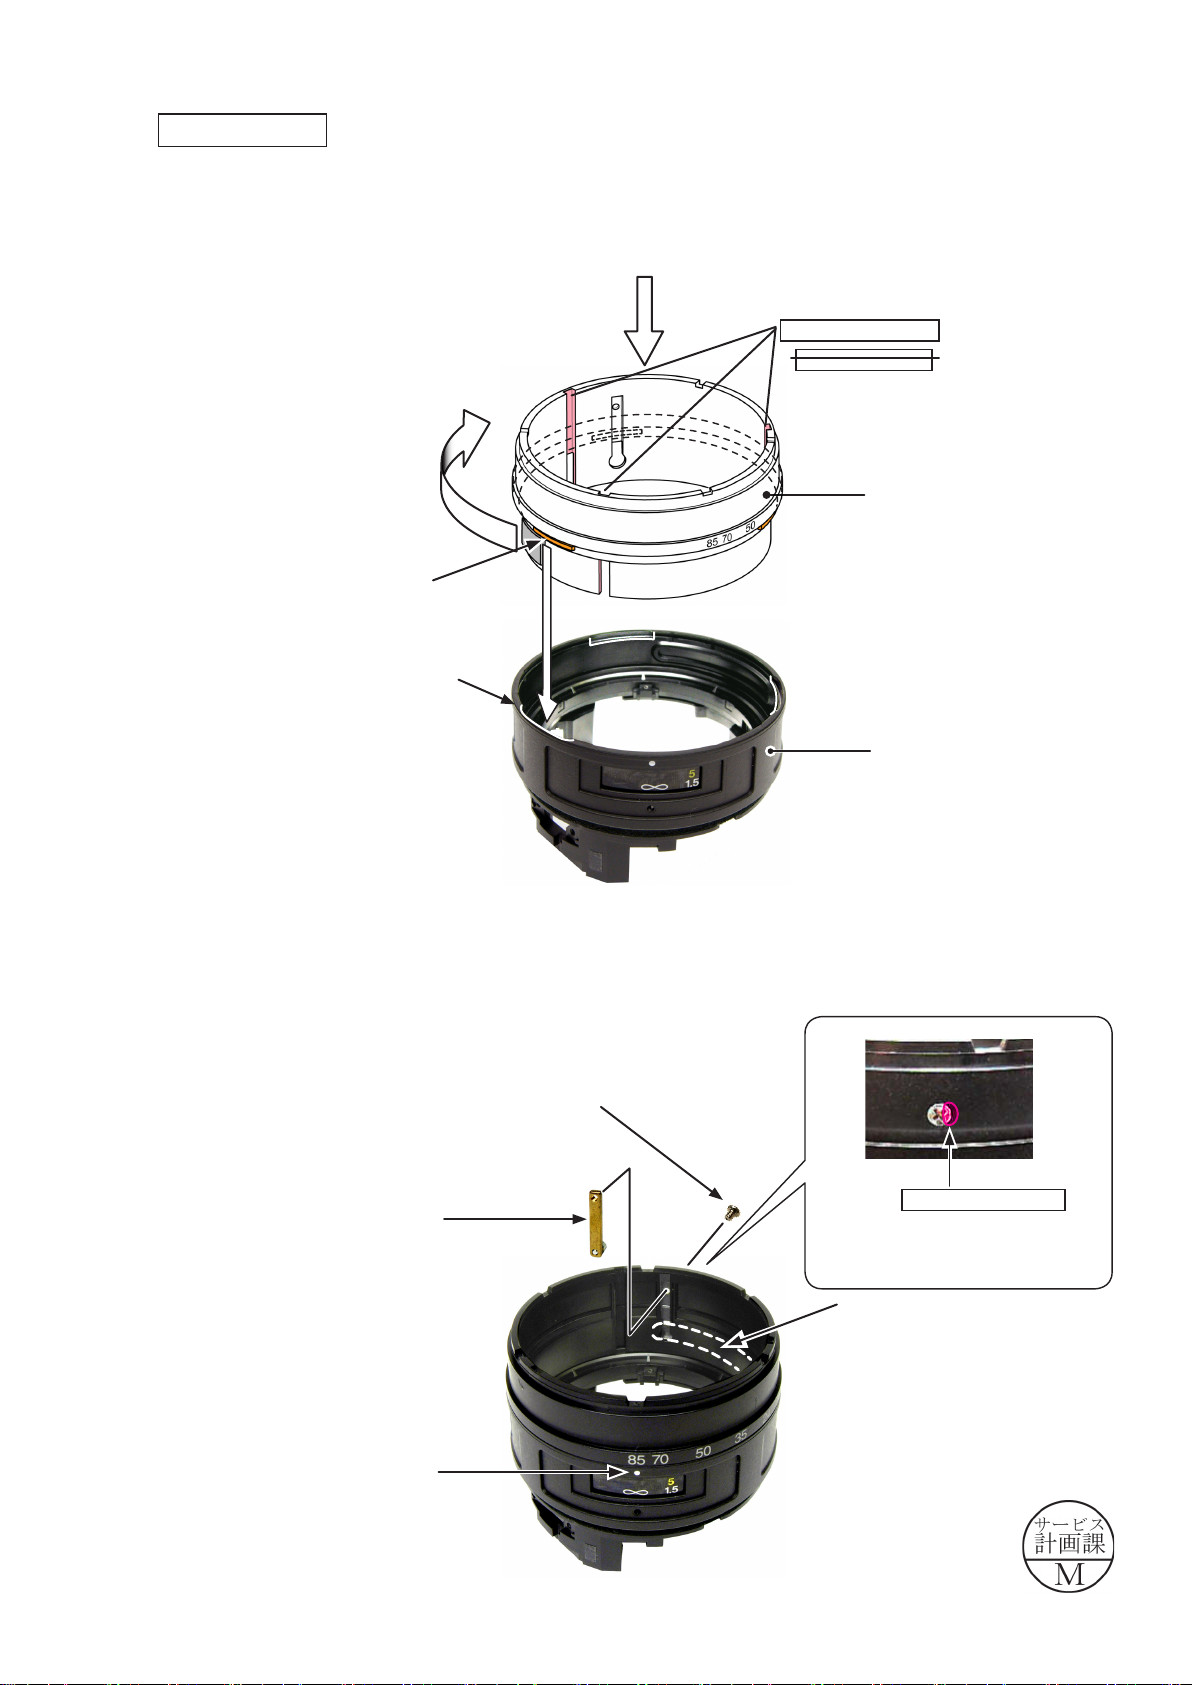
JAA80051-R.3741.A
INC
Zoom ring unit
Mount the zoom ring unit (B27) by tting its three protrusions with the three cutouts of the xed ring (#55)
・
and sit in the groove .
Turn the zoom ring unit (B27) clockwise, and align "85" of zoom index with the index of the xed ring
・
(#55).
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall three surfaces sliding
with [#110].
B27
Protrusion×3
Cutout×3
#55
Assemble the zoom control key (#140) by tting its lower part in the groove section (white dotted area) of
・
the xed ring (#55), and secure it with the screw (#144).
#144
#140
Leave as it is 15 mins. or more after
applying the adhesive.
Adhesive: Screwlock
Changed page △× 1
Index
- ・AF-S DX 6-85/3.5-5.6G VR -
Groove section
March�3�008�3�0083�008�008008
Page 37
JAA80051-R.3741.A
INC
Zoom ring unit (continued)
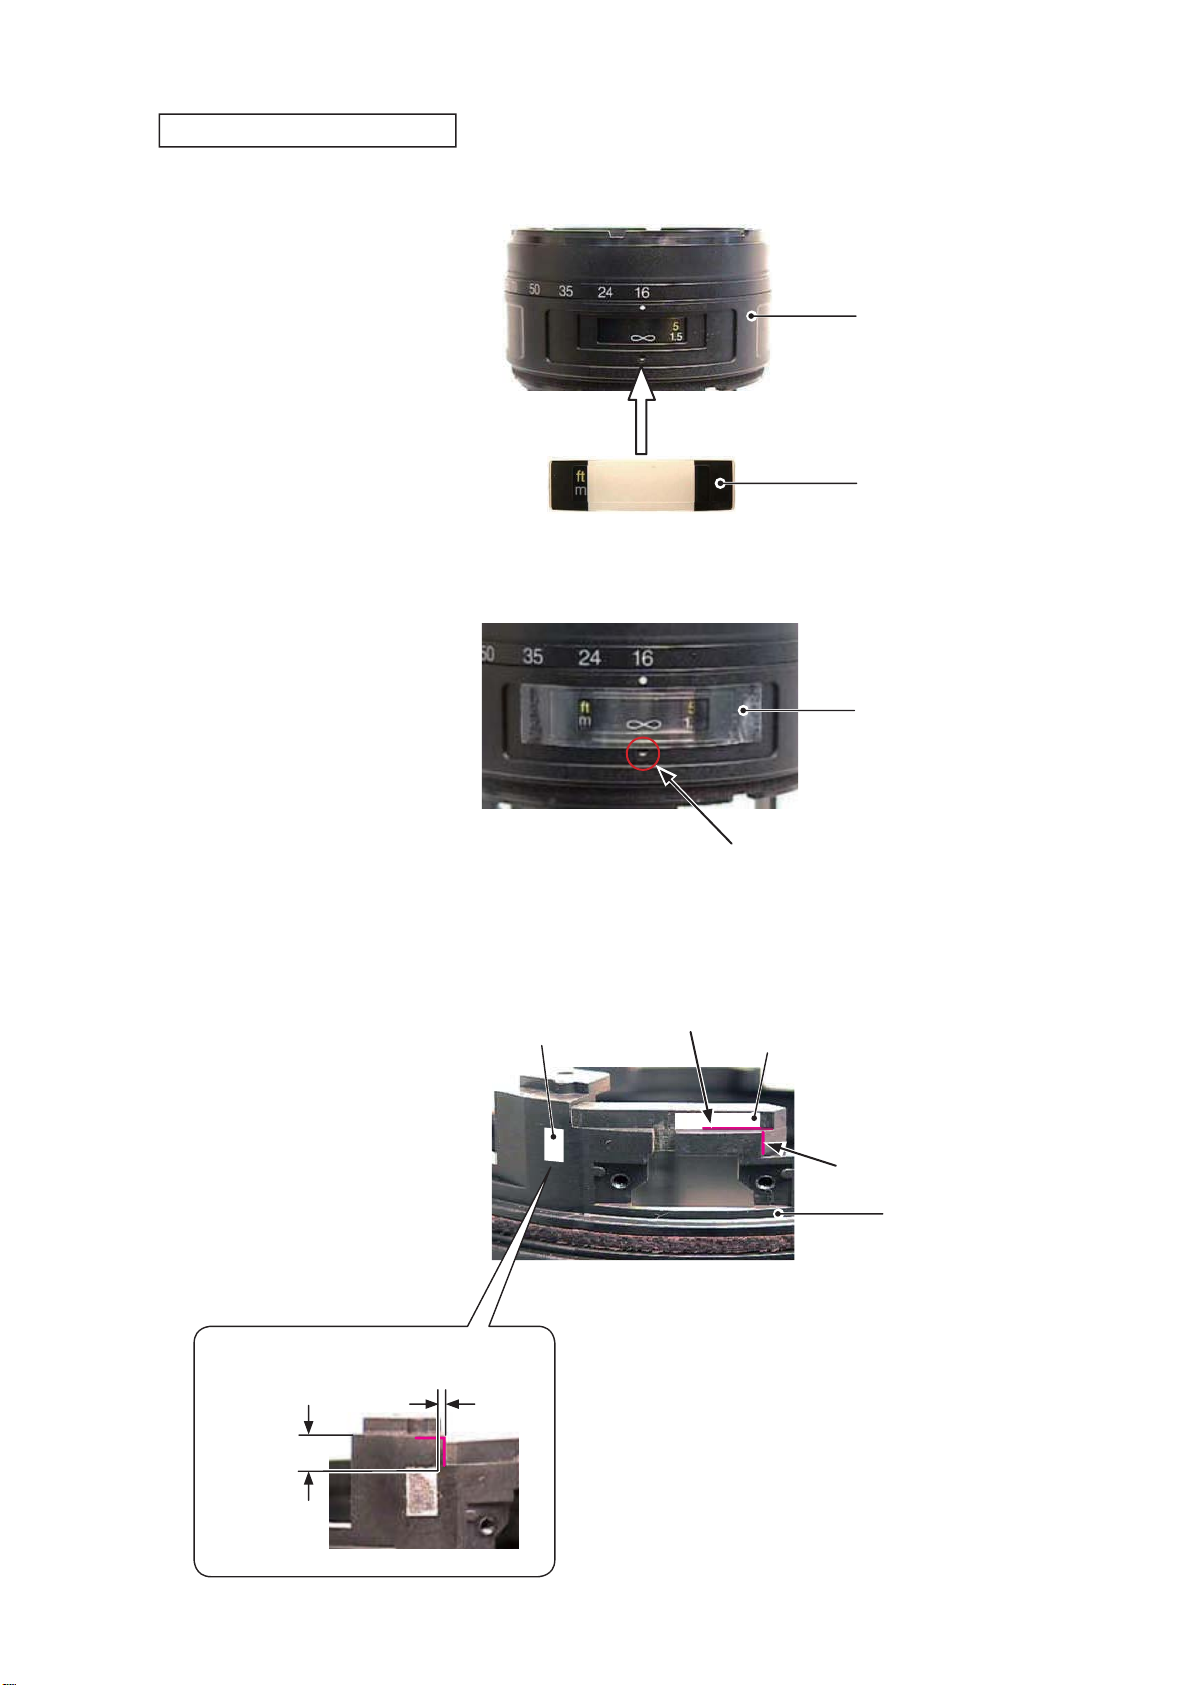
Attach the focus window (#76) to the fi xed ring (#55).
・
#55
#76
Attach the polyester tape (approx. 10×50 mm) on the focus window (#76) so as not to block [1.5 mm across]
・
hole.
φ1.5 hole
Attach the double-stick tape on the fi xed ring (#55) based on the reference position.
・
TA-0027
5×3
Reference
position
TA-0003
2×10
Reference position
#76
#55
Reference position
Approx. 1mm
Approx. 4mm
- A15・AF-S DX 16-85/3.5-5.6G VR -
Page 38
JAA80051-R.3741.A
INC
Zoom ring unit (continued)
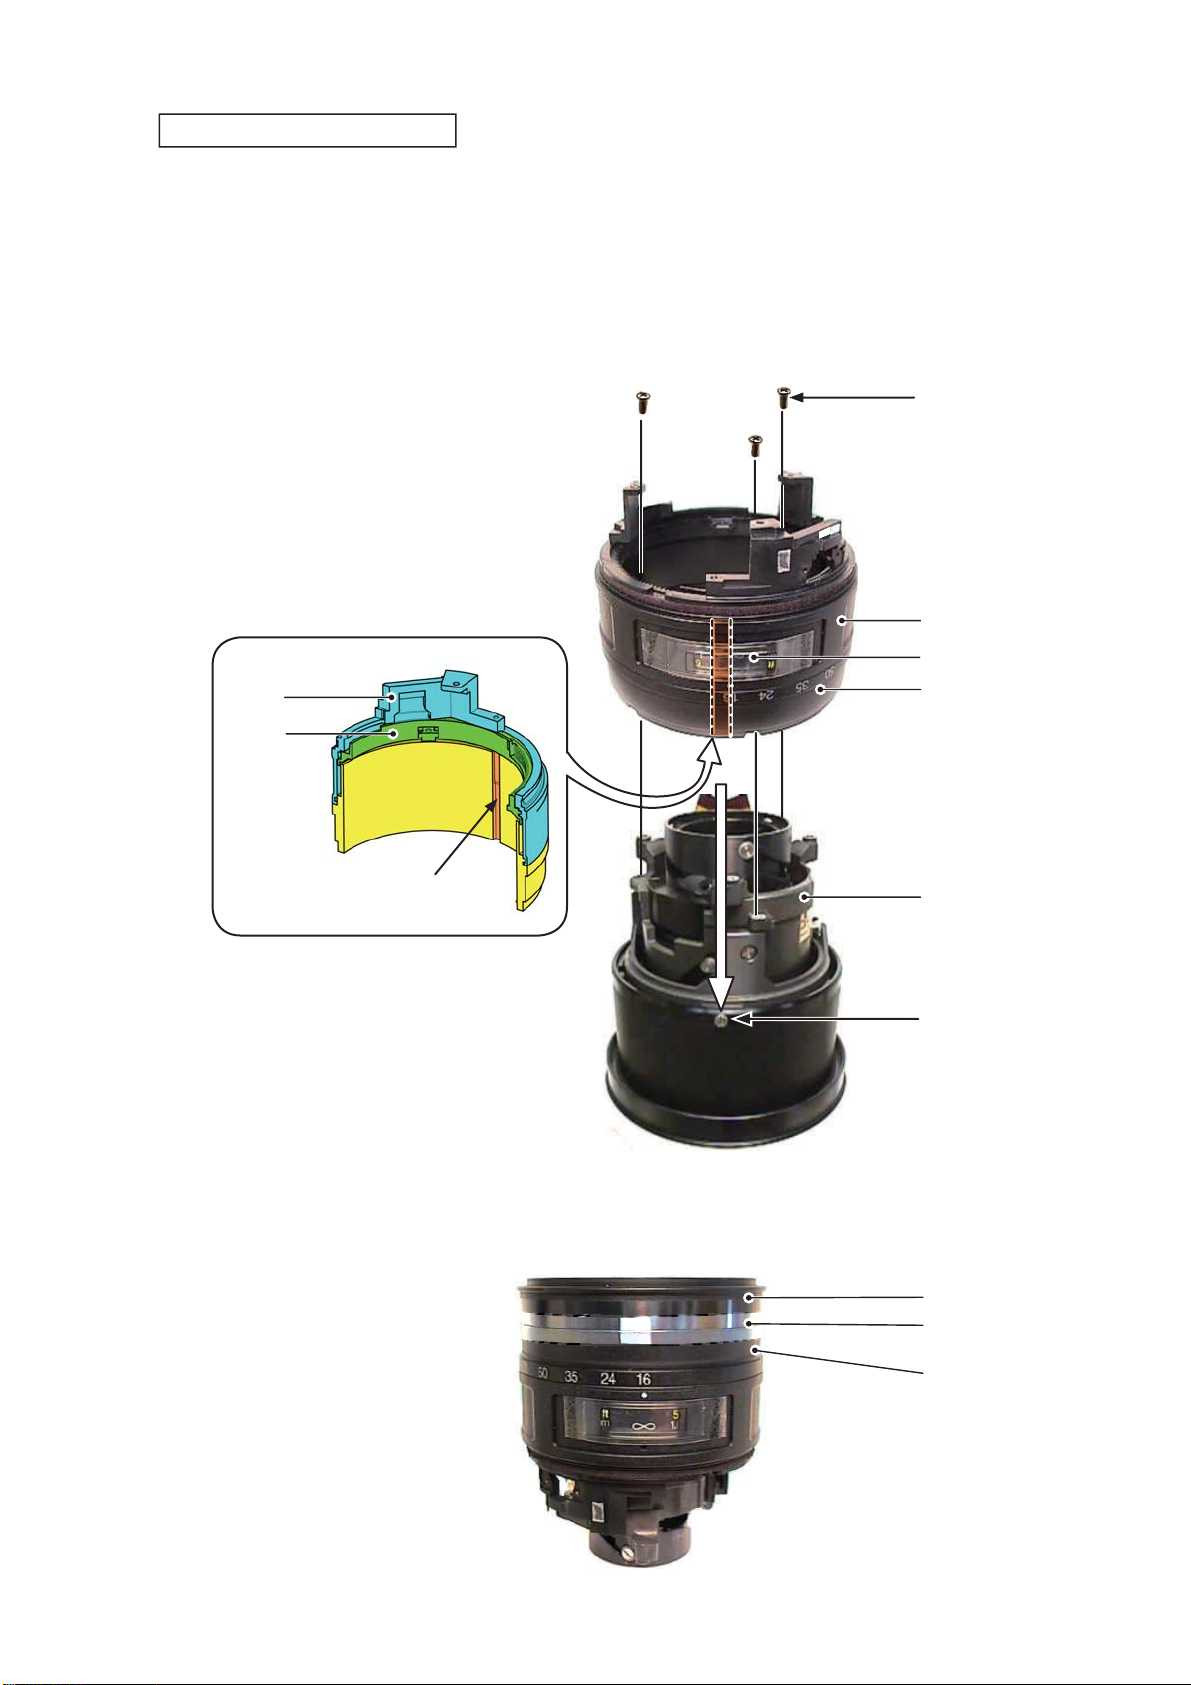
Set the fi xed tube (#50) to WIDE.
・
Set the zoom ring unit (B27) to WIDE.
・
Set the gear unit (B40) to "∞" (infi nity).
・
Align the positions of the three screws (#110) with the three inner straight grooves of the fi xed ring (#55),
・
and mount the zoom ring unit.
Tighten the three screws (#123) in numeric
・
order of ①, ②, and ③ by turning the zoom
①
②
#123×3
③
index ring clockwise for positioning and fi x it.
B27
B27
B40
Inner straight groove of [#55]
Wrap the tape around the support ring unit (B101) and zoom ring (#27) to fi x them.
・
B40
#55
#50
#110×3
B101
TA-0012
6×30
#27
- A16・AF-S DX 16-85/3.5-5.6G VR -
Page 39
JAA80051-R.3741.A
INC
Focus key
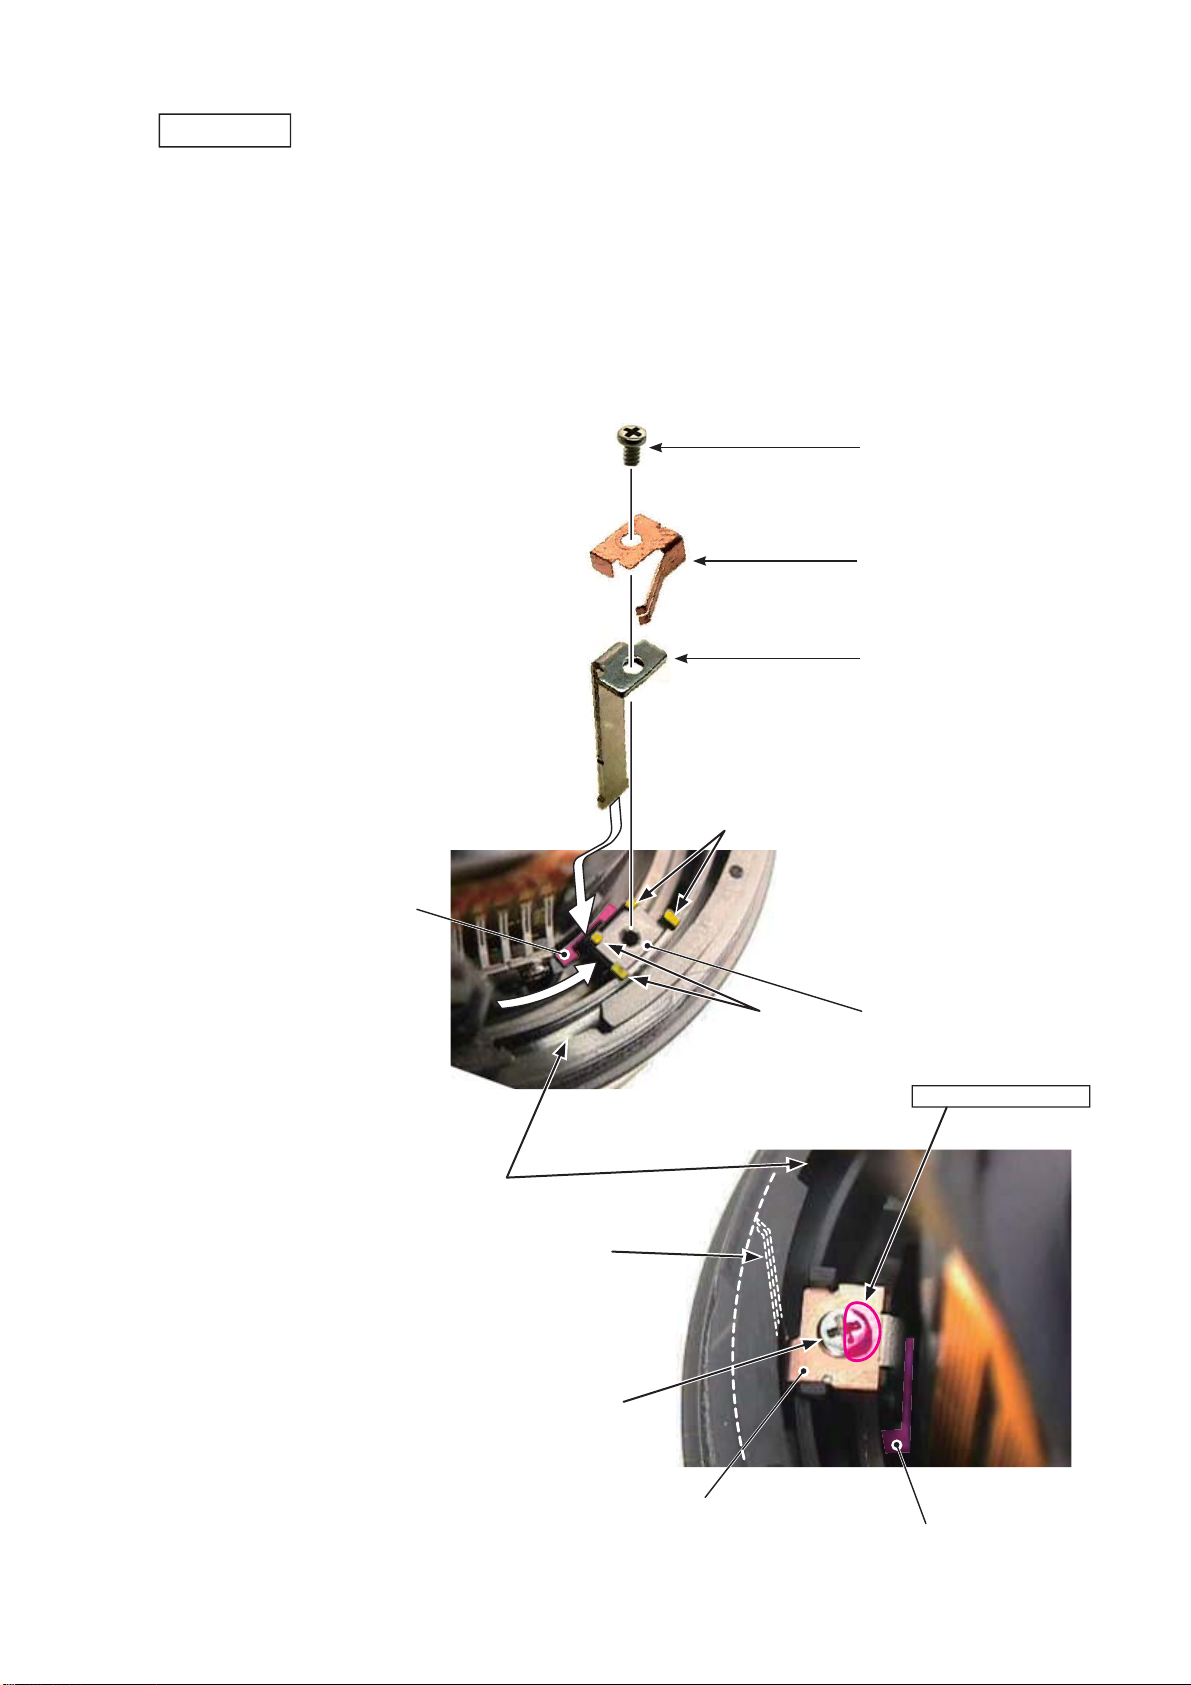
Insert the focus key (#54) into the groove of the lever section of the 2nd lens-G cam ring (#25).
・
Turn the gear unit (B40) to "∞" (infi nity).
・
Fit the head of the focus key (#54) with the four protrusions of the gear unit (B40).
・
Place the plate spring (#157) on the focus key (#54).
・
Secure the focus key (#54) and plate spring (#157) with the screw (#122).
・
Apply the adhesive to the head of the screw (#122) and fi x it.
・
#122
#157
Lever section of
[#25]
Insert the lower part (spring section)
#54
Protrusion×2 of [B40]
B40
Protrusion×2
Adhesive: Screwlock
of the plate spring (#157) into the
cutout of the zoom ring unit (B27)
fi rst, then move [#157] to be inside
the groove as shown in the right
picture.
- A17・AF-S DX 16-85/3.5-5.6G VR -
Spring section
#122
#157
Lever section of [#25]
Page 40
JAA80051-R.3741.A
INC
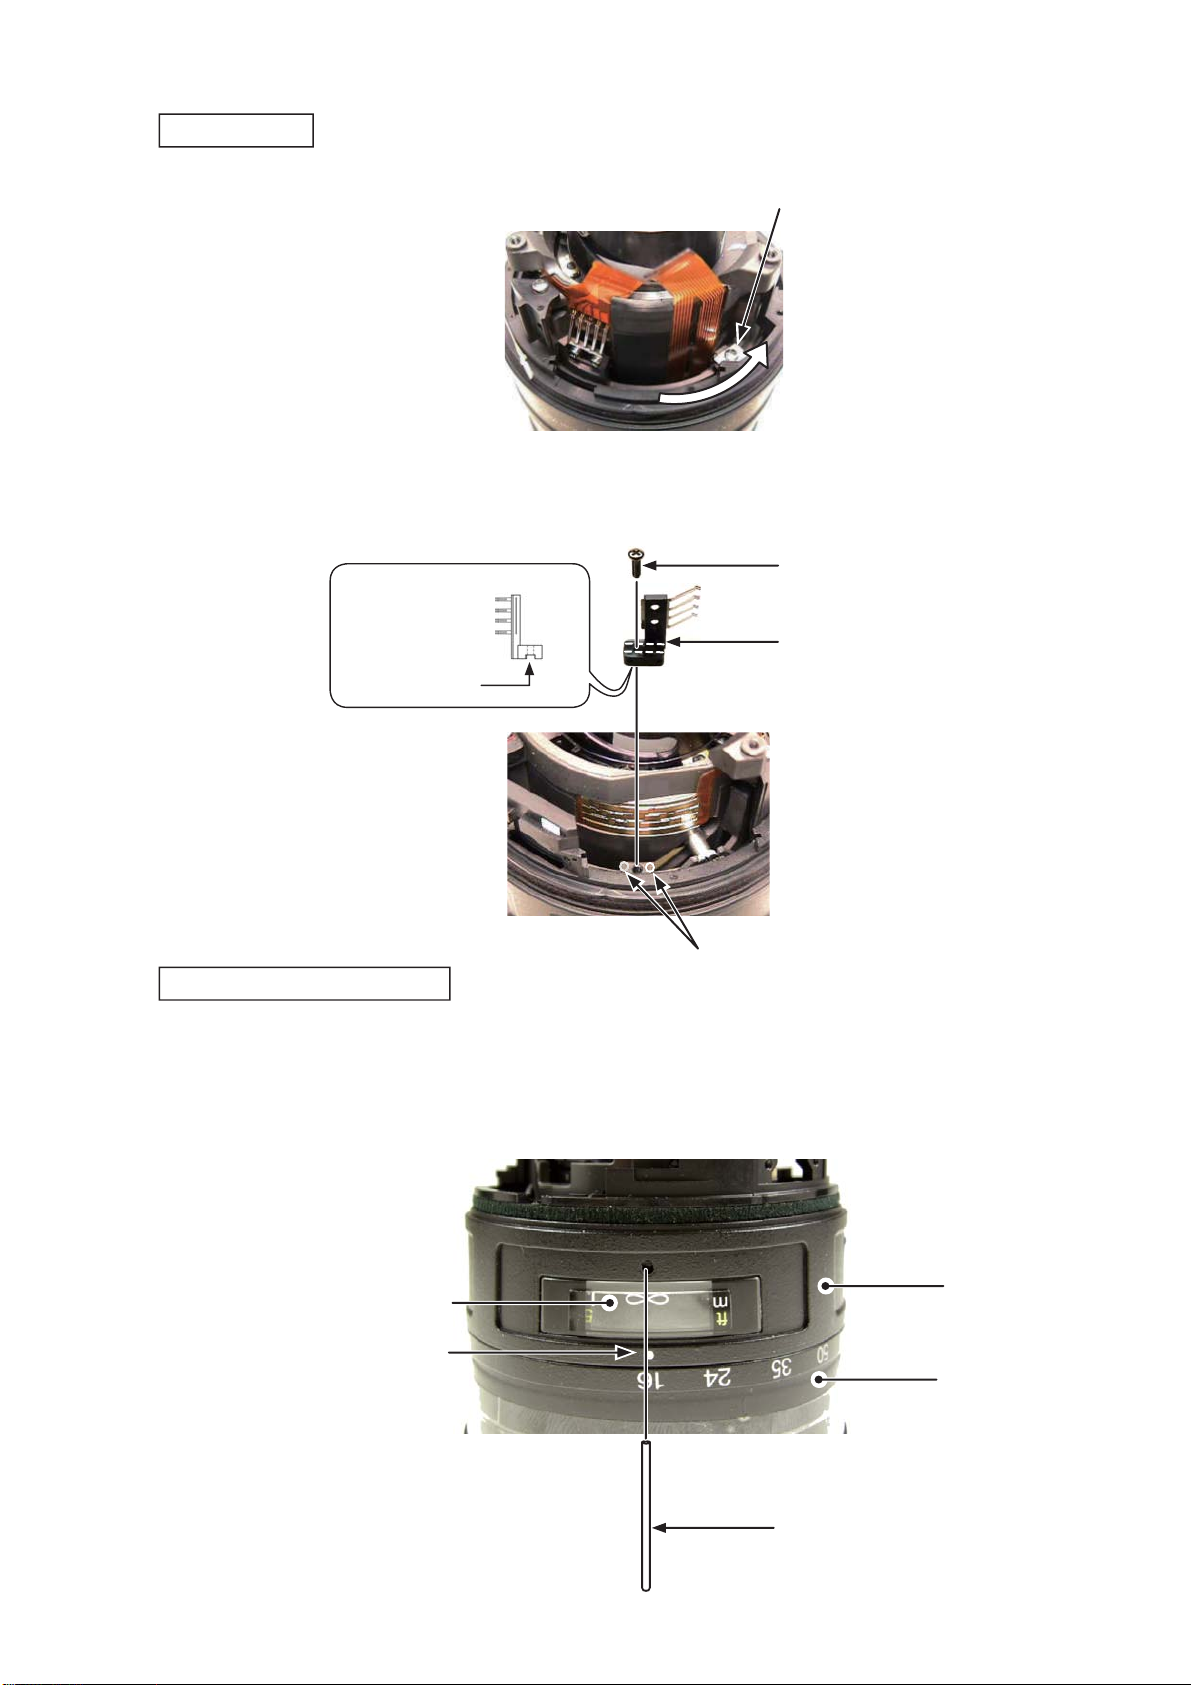
Focus brush
Move the focus key (#54) in the direction of the arrrow (CLOSE).
・
Put the focus brush (B105) by fi tting the protrusion of the gear unit (B40) in the groove section of [B105].
・
Tighten the screw (#145).
・
#54
Rear view of [B105]
Groove section
Protrusion of [B40]
Positioning of Focus encoder
Move the focus key (#54) and align "∞" position of the focus index (#49) with the below index.
・
Insert the reference pin (J11349) into "φ1.5 hole" of the fi xed ring (#55) and fi x the focus index.
・
Set the zoom ring (#27) to WIDE.
・
#145
B105
Caution:
Do NOT deform the brush.
・
Do NOT use a deformed brush.
・
#49
Index
- A18・AF-S DX 16-85/3.5-5.6G VR -
#55
#27
J11349
Page 41
JAA80051-R.3741.A
INC
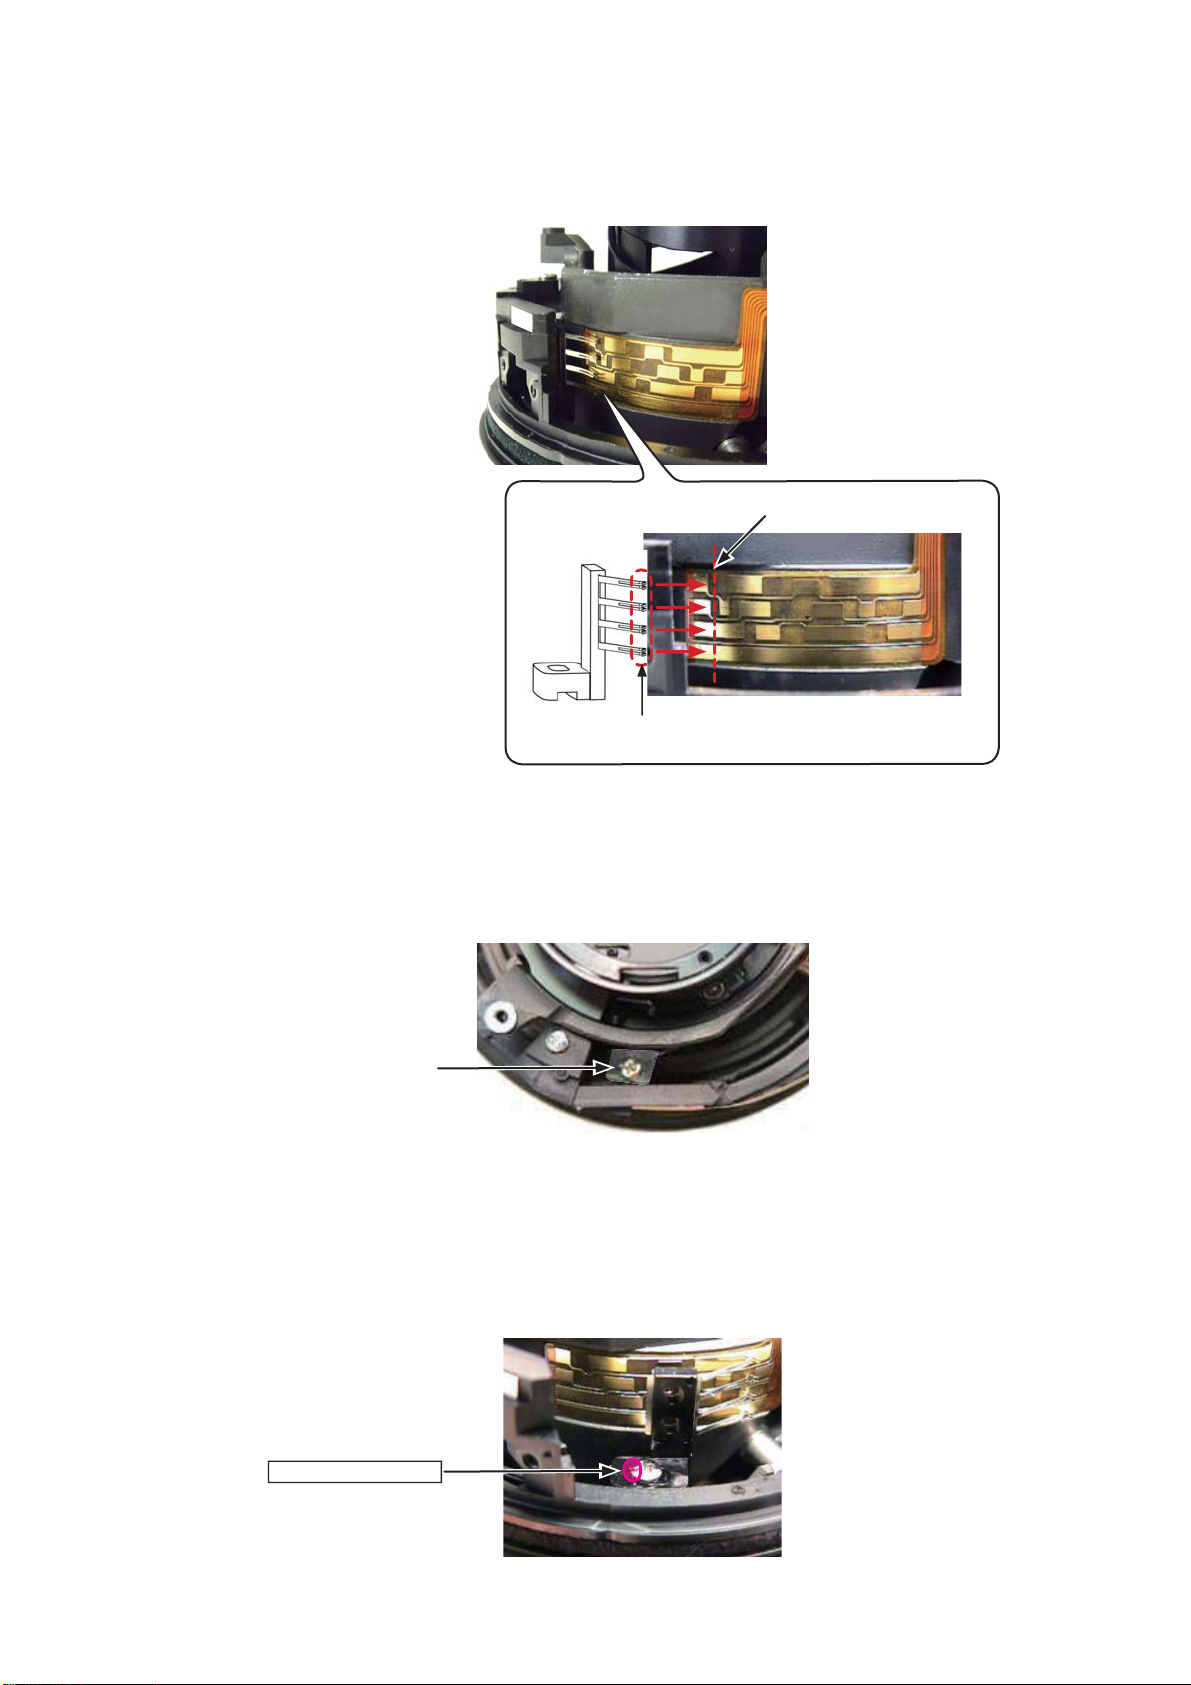
Match "∞" position of the focus encoder’s pattern with the brush tip ("R" section) of the focus brush (B105)
・
as below.
"∞" position of Focus-encoder’s pattern
Brush tip ("R" section) of [B105]
Tighten the screw (#145).
・
#145
Set the focus brush (B105) to CLOSE-end, and apply the adhesive to the head of the screw (#145).
・
Adhesive: Screwlock
#145
- A19・AF-S DX 16-85/3.5-5.6G VR -
Page 42
JAA80051-R.3741.A
INC
GMR sensor
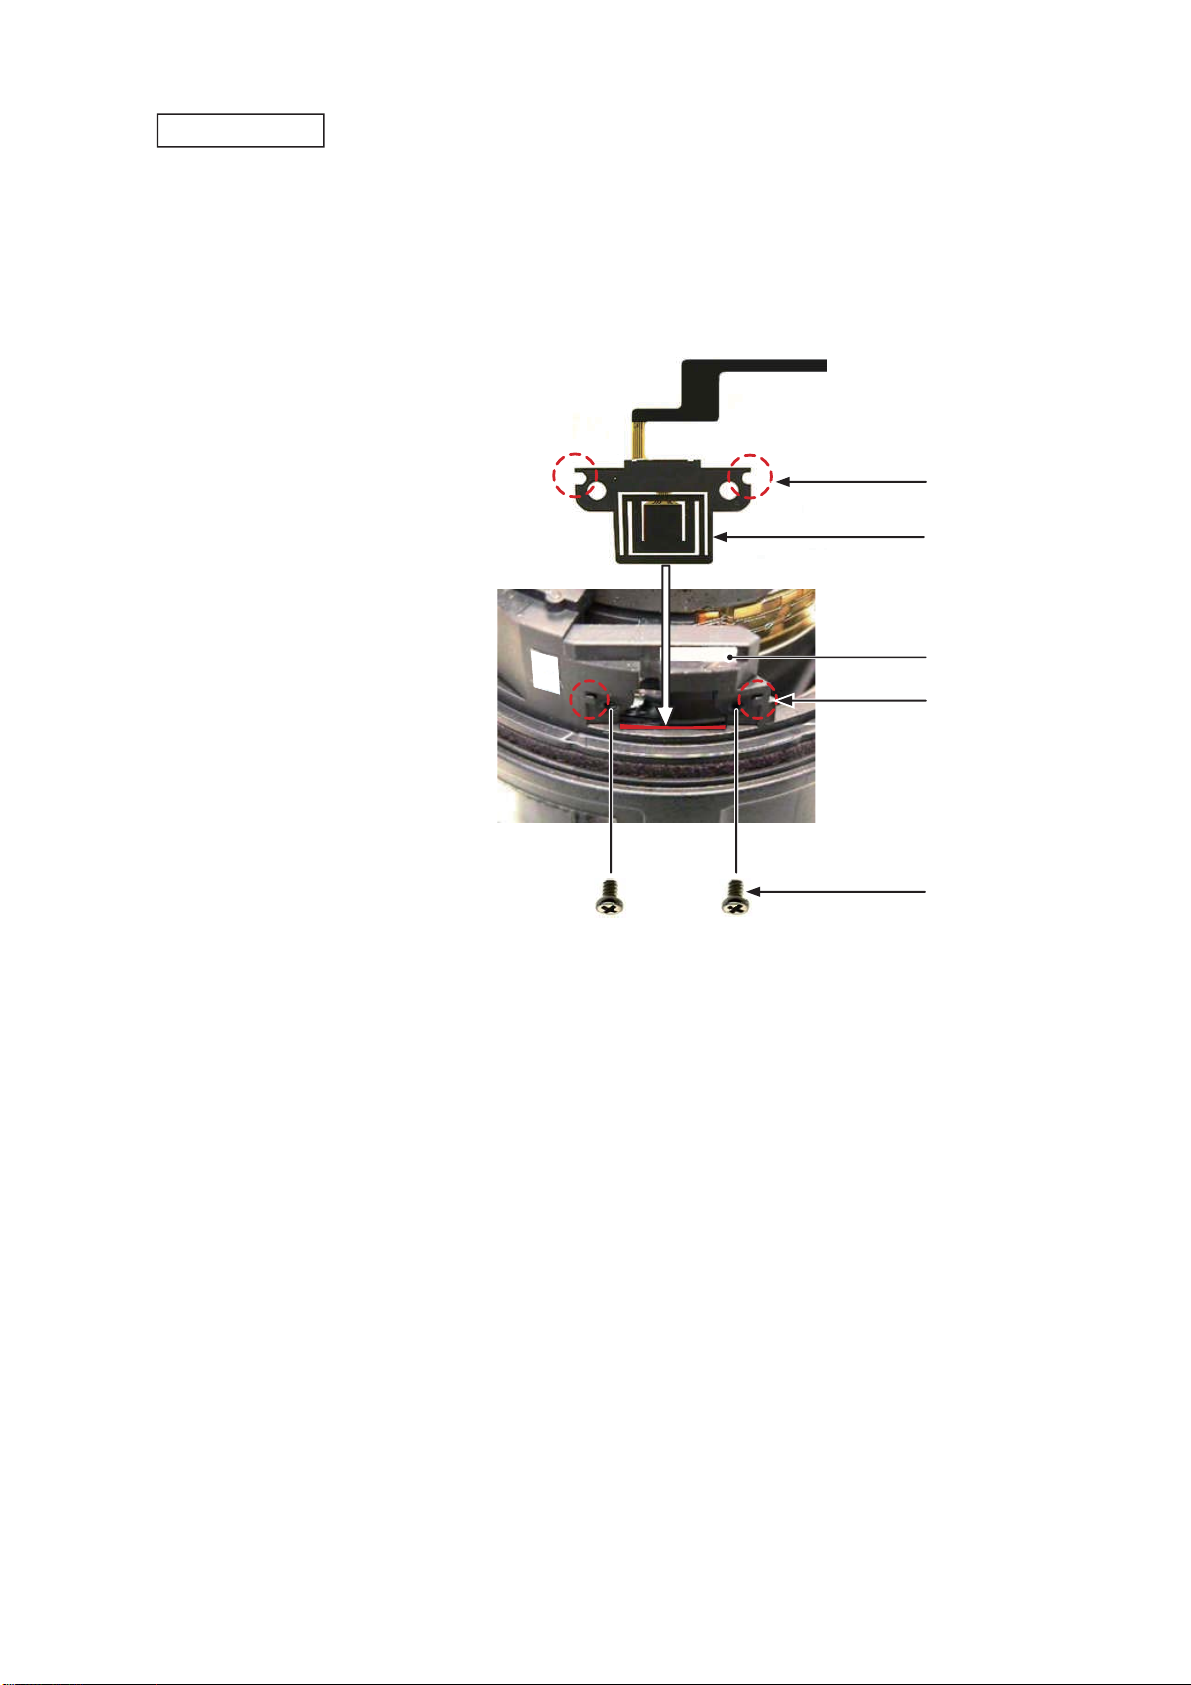
Insert the edge of GMR sensor (#1011) into the gap of the fi xed ring (#55) and fi t the two cutouts of GMR
・
sensor with the two protrusions of the fi xed ring (#55).
Tighten the two screws (#91).
・
Attach the double-stick tape (TA-0003) on the FPC of GMR sensor.
・
Cutout×2
#1011
TA-0003
2×10
Protrusion ×2
#91×2
- A20・AF-S DX 16-85/3.5-5.6G VR -
Page 43
JAA80051-R.3741.A
INC
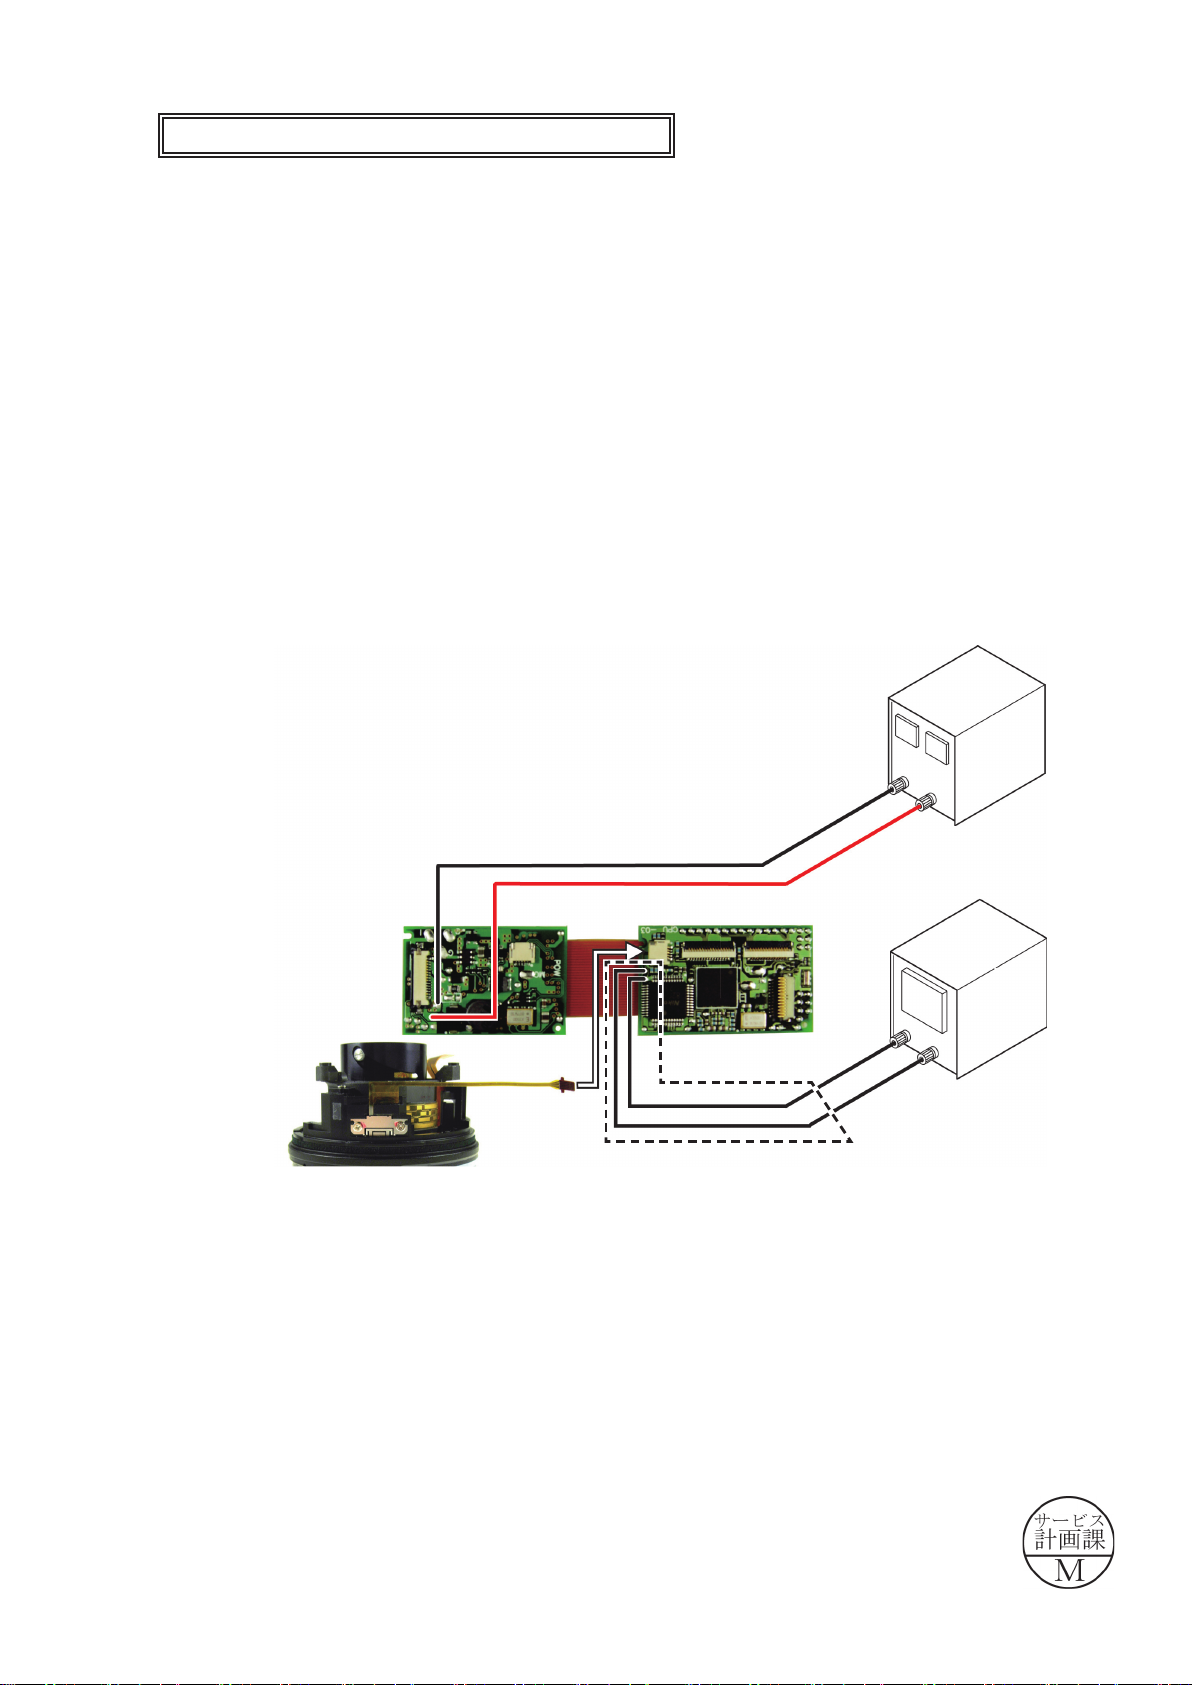
Inspection and Adjustment of GMR output waveform
● When GMR unit is disassembled and replaced, be sure to make inspection and adjustment.
1. Device:
Caution:
Single-output rated voltage power-supply
Oscilloscope
GMR output inspection tool 1 unit Self-made tool (ref. T3)
1 unit: 5V 100mA
1 unit
If there are problems with conduction between the contacts of the GMR output inspection
tool and the relay-FPC, the contacting surface of the relay FPC may be dirty, eroded, or
oxidized. So polish the contacts and connect them.
2. Preparation of the lens for measurement
Connect the xed tube, which has GMR unit assembled, to each measuring instrument.
Refer to T3 for wiring on Main PCB.)
Rated voltage
power-supply
△ (Revision)
Oscilloscope
(2ch type)
Set value
5.0 V
100 mA
△× 1
Page 44
JAA80051-R.3741.A
INC
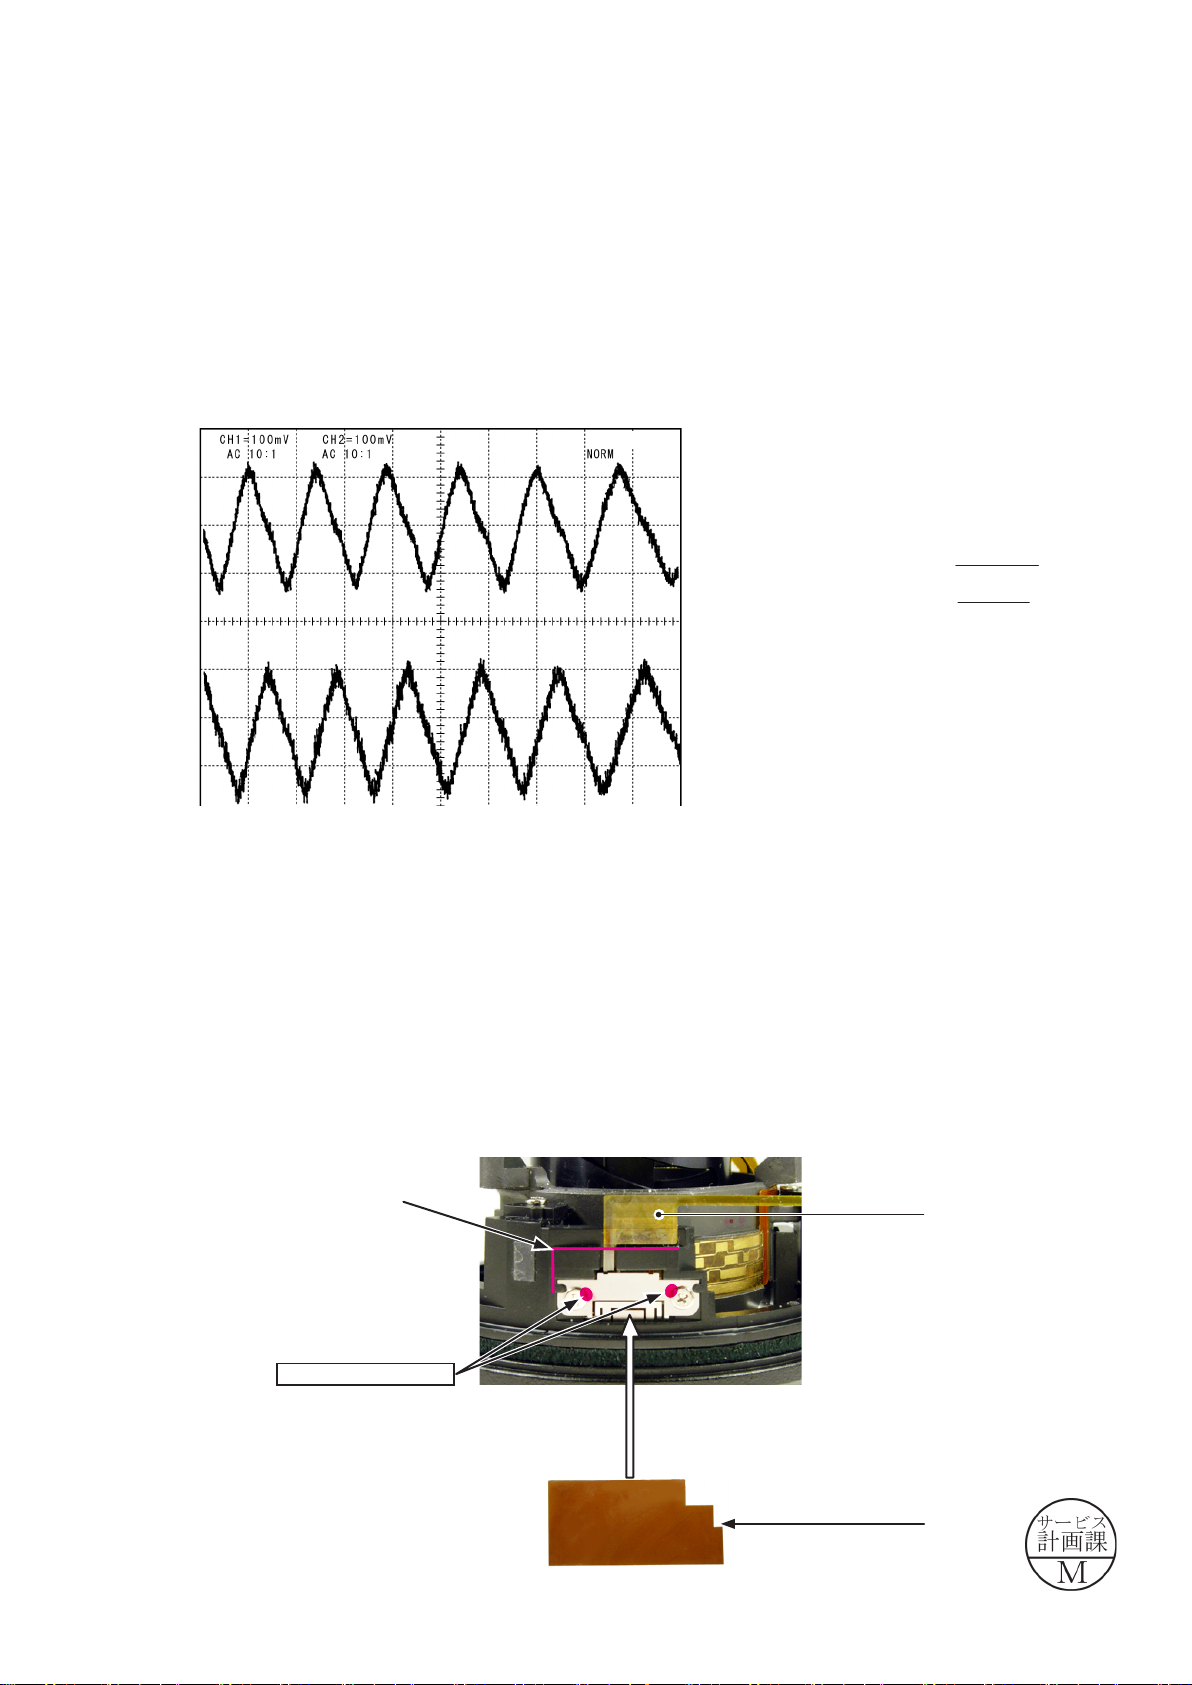
3How to inspect and adjust:
Conrm that the electric current and voltage of the connected rated voltage power-supply are set
values, then turn it ON.
Set the oscilloscope, and turn the focus turning-tube with hand.
In case large waveform-noise is detected, use the FILTER function.
How to set FILTER function (e.g. DL1540 manufactured by YOKOGAWA
1. Press the FILTER button.
2. Select “Smooth” of the menu on screen and turn it ON.
1 m s / d i v
●
Oscilloscope setting
V/Div (ch1) : 100 mV
V/Div (ch2) : 100 mV
Coupling : AC
Time/Div : 20ms/div
1ms/div
Trigger Mode : NORMAL
Trigger Coupling : AC
Trigger Source : : CH1
Trigger Position : + 4 div
Trigger Type : EDGE
Trigger Level : 0V
INPUT (ch1) : AC
INPUT (ch2) : AC
△ (Revision)
Standard: Amplitude of all pulses/waveforms is 150mV or more.
Note: Check the waveform by rotating the focus turning-tube all the way around back and forth.
If there is no problem with the waveform of GMR sensor, apply the adhesive to the head of the two screws
(#91) to x.
Attach the tape (#138) on the GMR sensor.
Reference position for
attaching [#138]
Adhesive: Screwlock
#91×2
FPC of [#1011]
#138
△× 1
Page 45
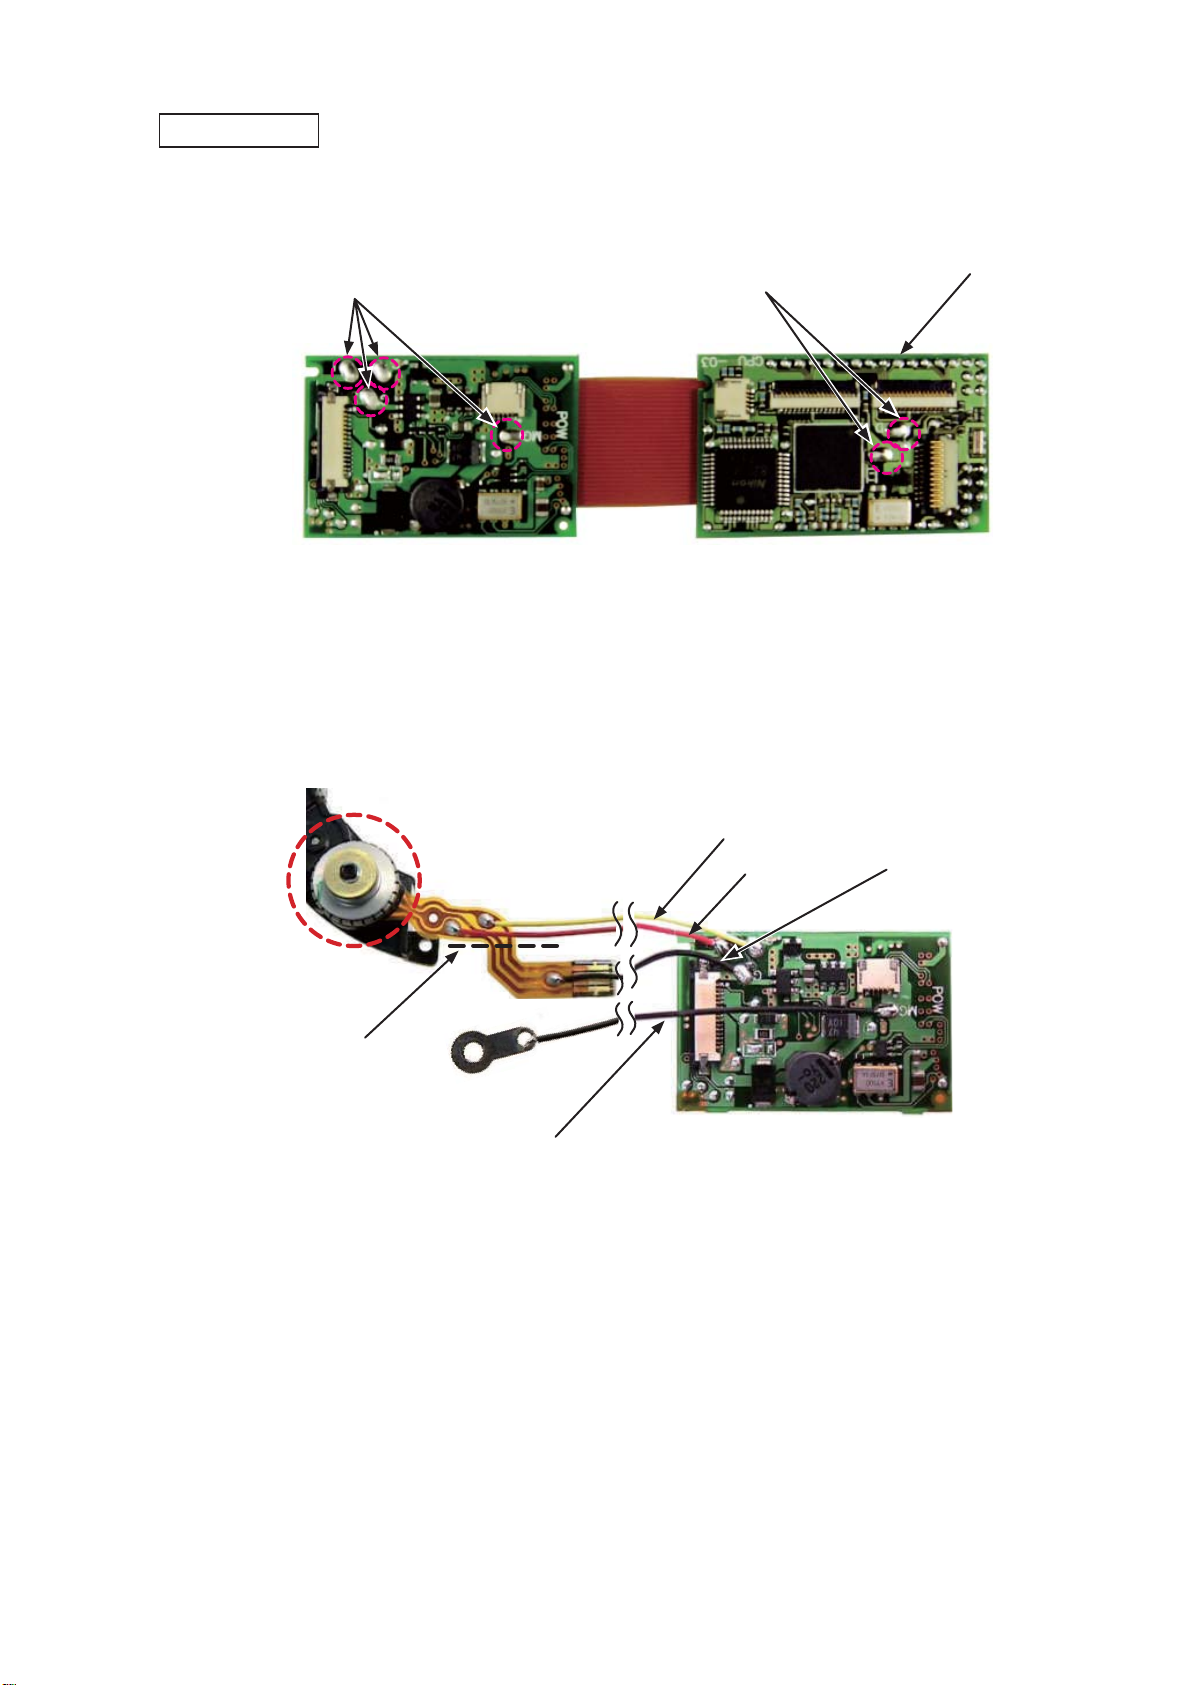
Main PCB
INC
Make six pre-solderings on the main PCB (B1001).
・
JAA80051-R.3741.A
Pre-soldering here
Make a fold on the FPC of SWM unit (B501) as below.
・
Solder the three lead wires of SWM unit and the lead wire of the lug plate unit (B1028) on the main PCB.
・
Caution: Do NOT touch "A" area.
"A" area
Pre-soldering here
#1030(yellow
#1029(red
)
)
#1031(black
B1001
)
FPC of [B501]
Mountain-fold
B1028
- A23・AF-S DX 16-85/3.5-5.6G VR -
Page 46
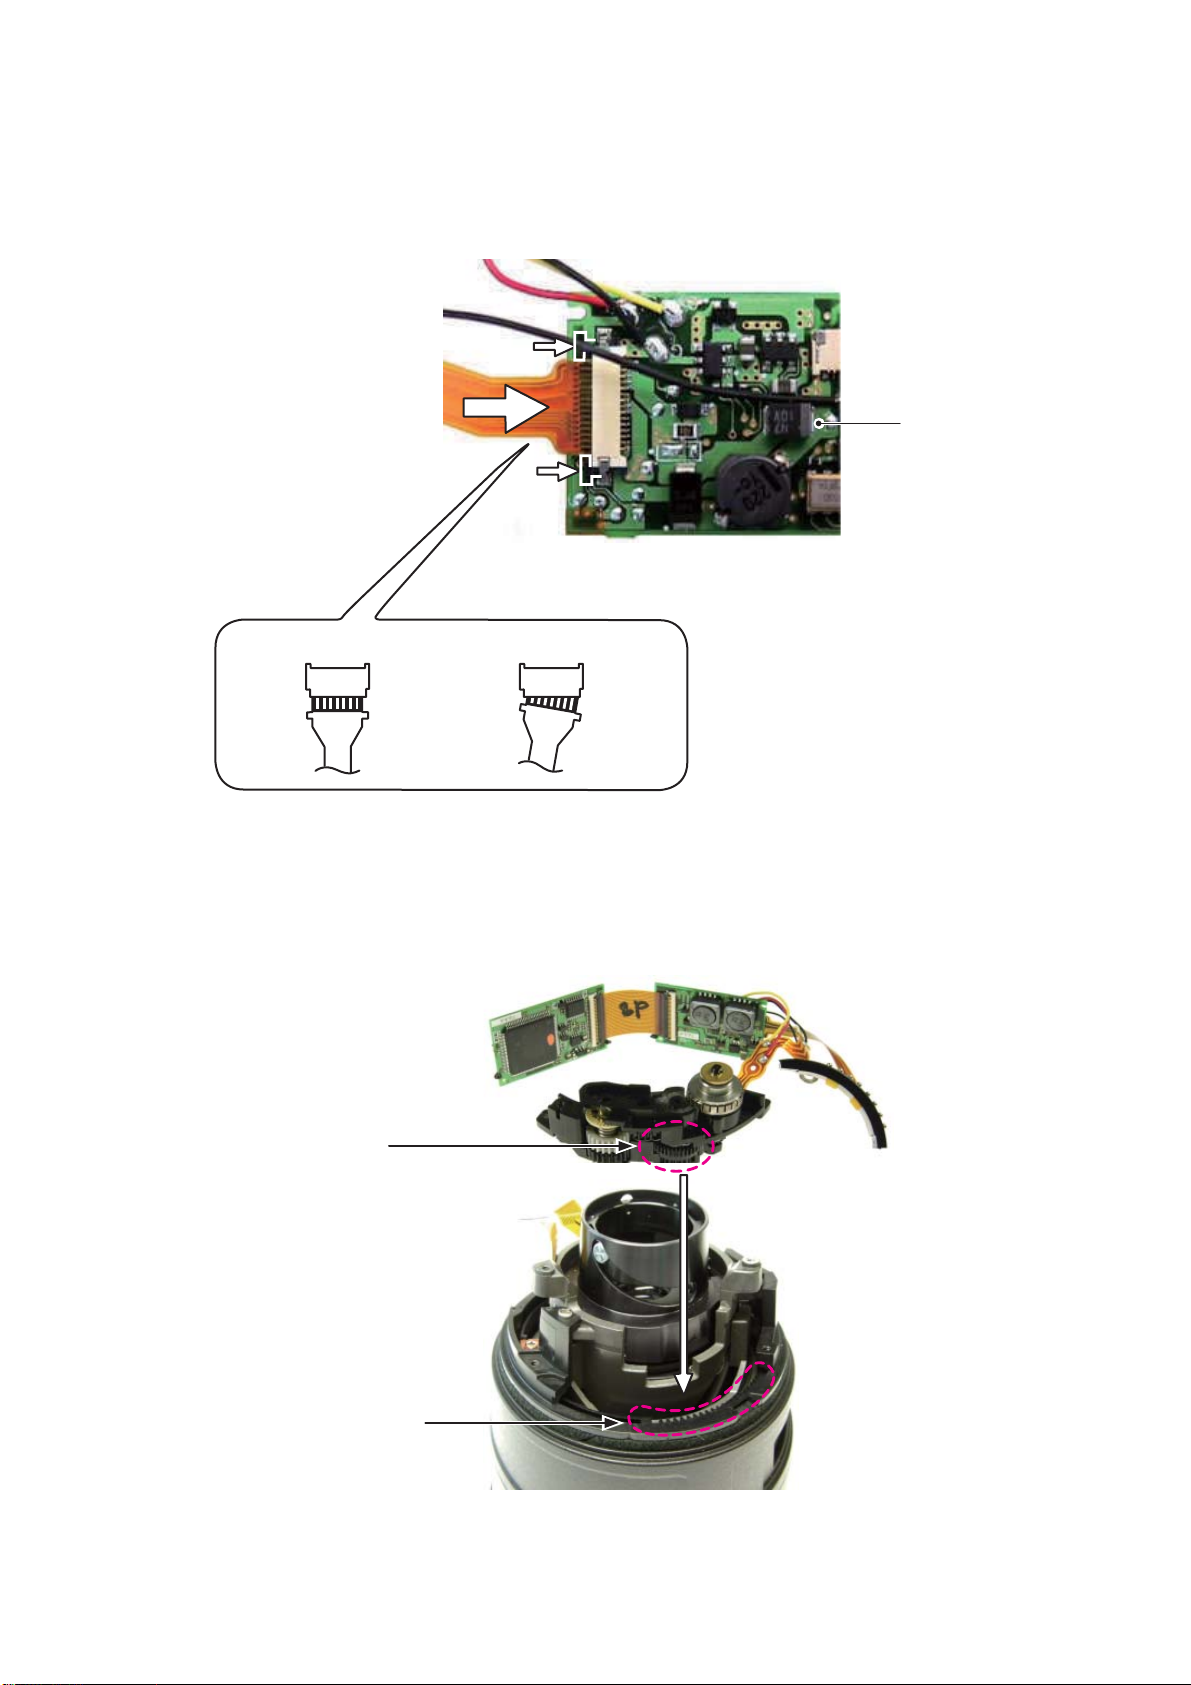
Connect the FPC of the contact unit to the connector of the main PCB (B1001).
INC
・
Caution: After connecting the FPC, be sure to lock the connector.
Lock here.
Lock
here.
JAA80051-R.3741.A
B1001
Insert FPC all the way
seated in.
Assemble SWM unit and gear unit by fi tting "A" area with "B" area.
・
"A" area
Do NOT insert FPC sideways.
"B" area
- A24・AF-S DX 16-85/3.5-5.6G VR -
Page 47
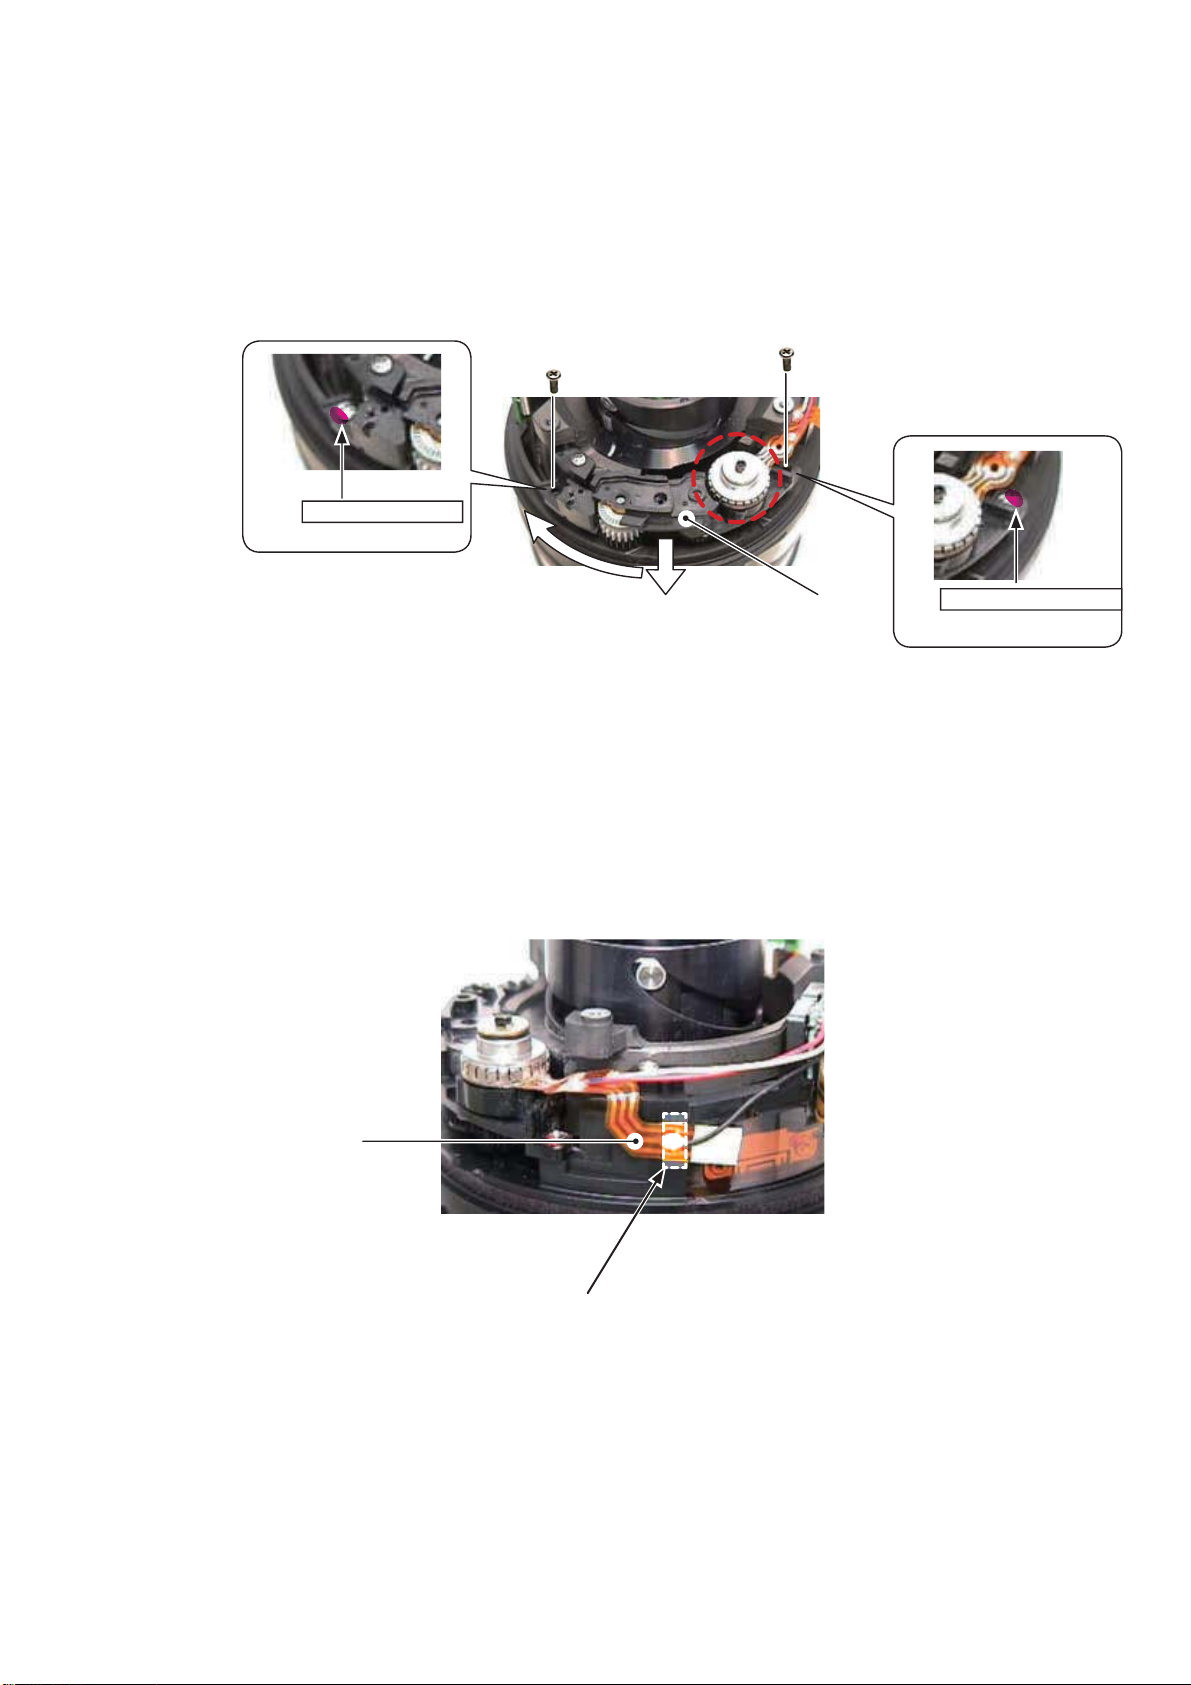
JAA80051-R.3741.A
A
INC
Push SWM unit (B501) toward outside by turning clockwise for positioning, and tighten the two screws
・
(#145).
Apply the adhesive to the head of the screw (#145).
・
Caution: Do NOT touch "A" area.
#145×2
A
Adhesive: Screwlock
#145
Direction of positioning
Peel off the backing paper of the double-stick tape, and attach the SWM-FPC by pressing it with a fi nger.
・
SWM FPC
B501
Adhesive: Screwlock
#145
Double-stick tape
- A25・AF-S DX 16-85/3.5-5.6G VR -
Page 48
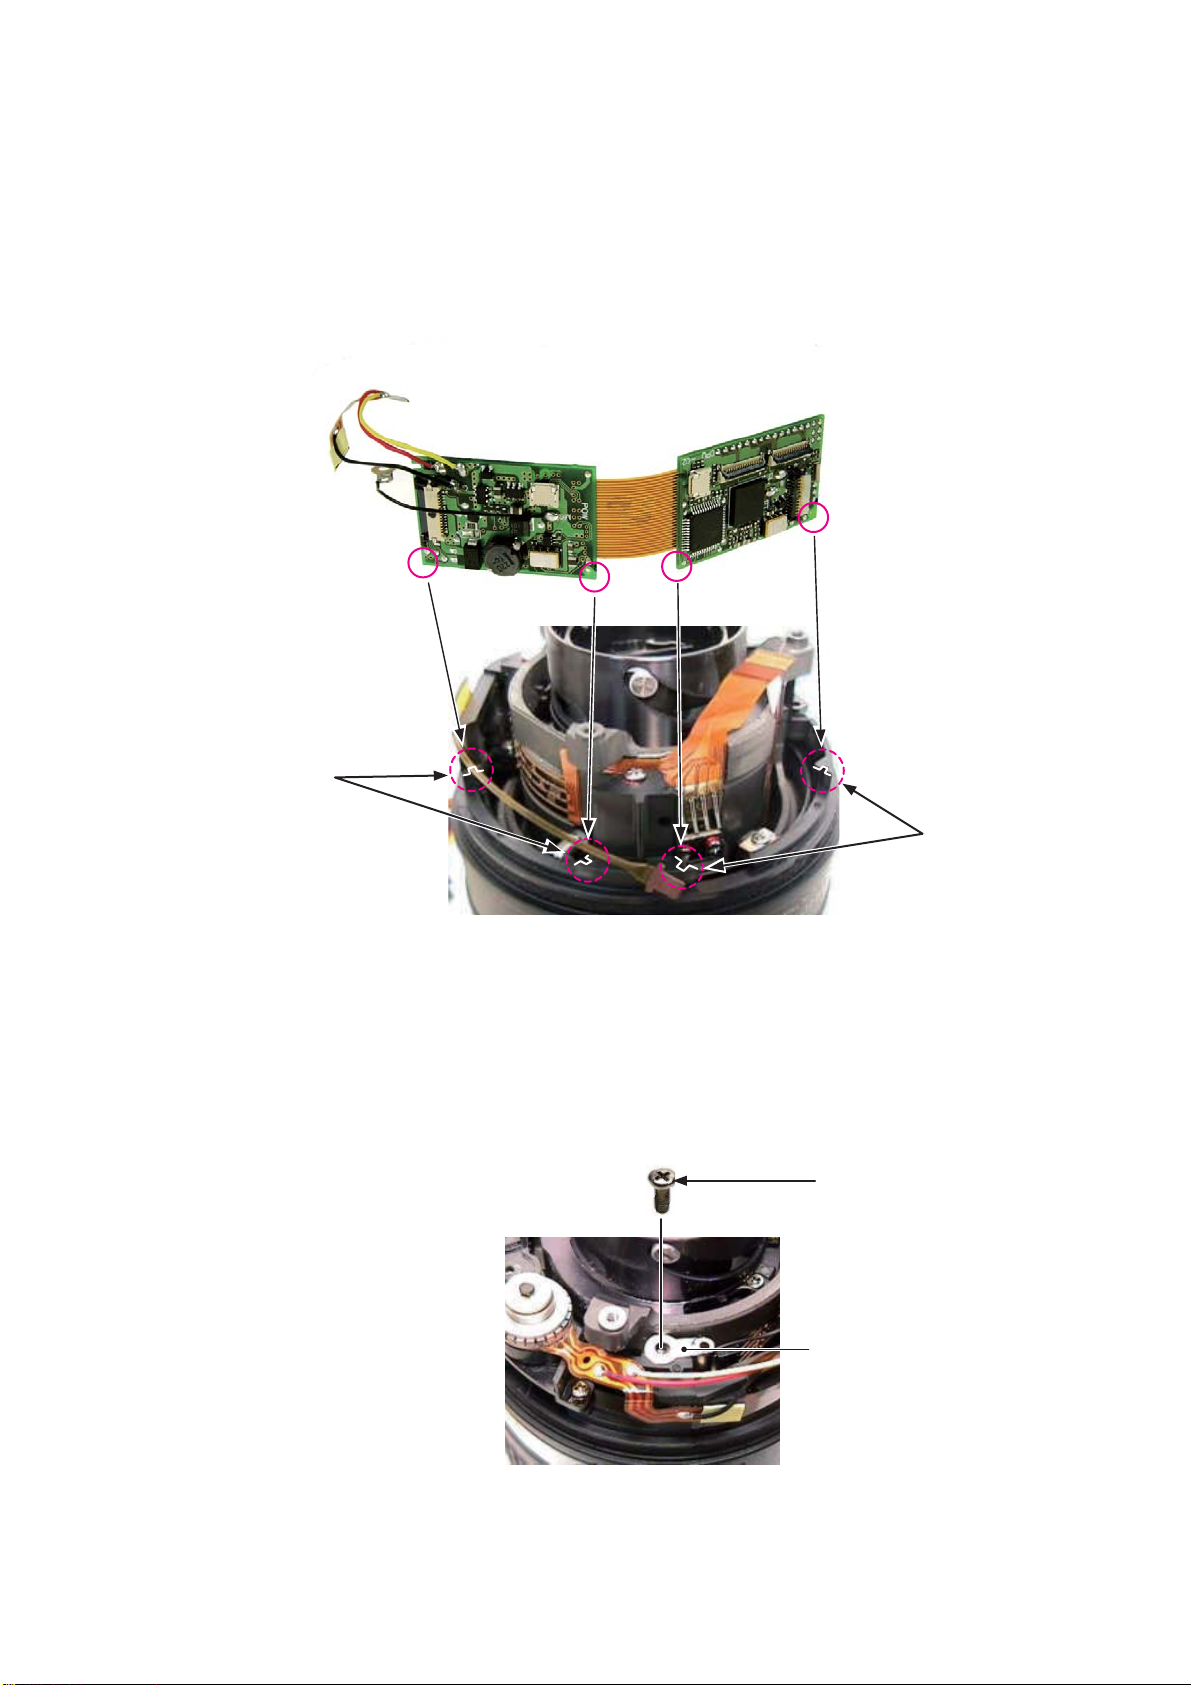
JAA80051-R.3741.A
INC
Being careful NOT to touch the GMR-FPC, mount the main PCB (#1001) on the fi xed ring (#55) by fi tting
・
with four cutouts.
Cutout at 2 places
Cutout at 2 places
Take out the screw (#123) and attach the lug plate unit (B1028) and tighten the screw again.
・
#123
B1028
- A26・AF-S DX 16-85/3.5-5.6G VR -
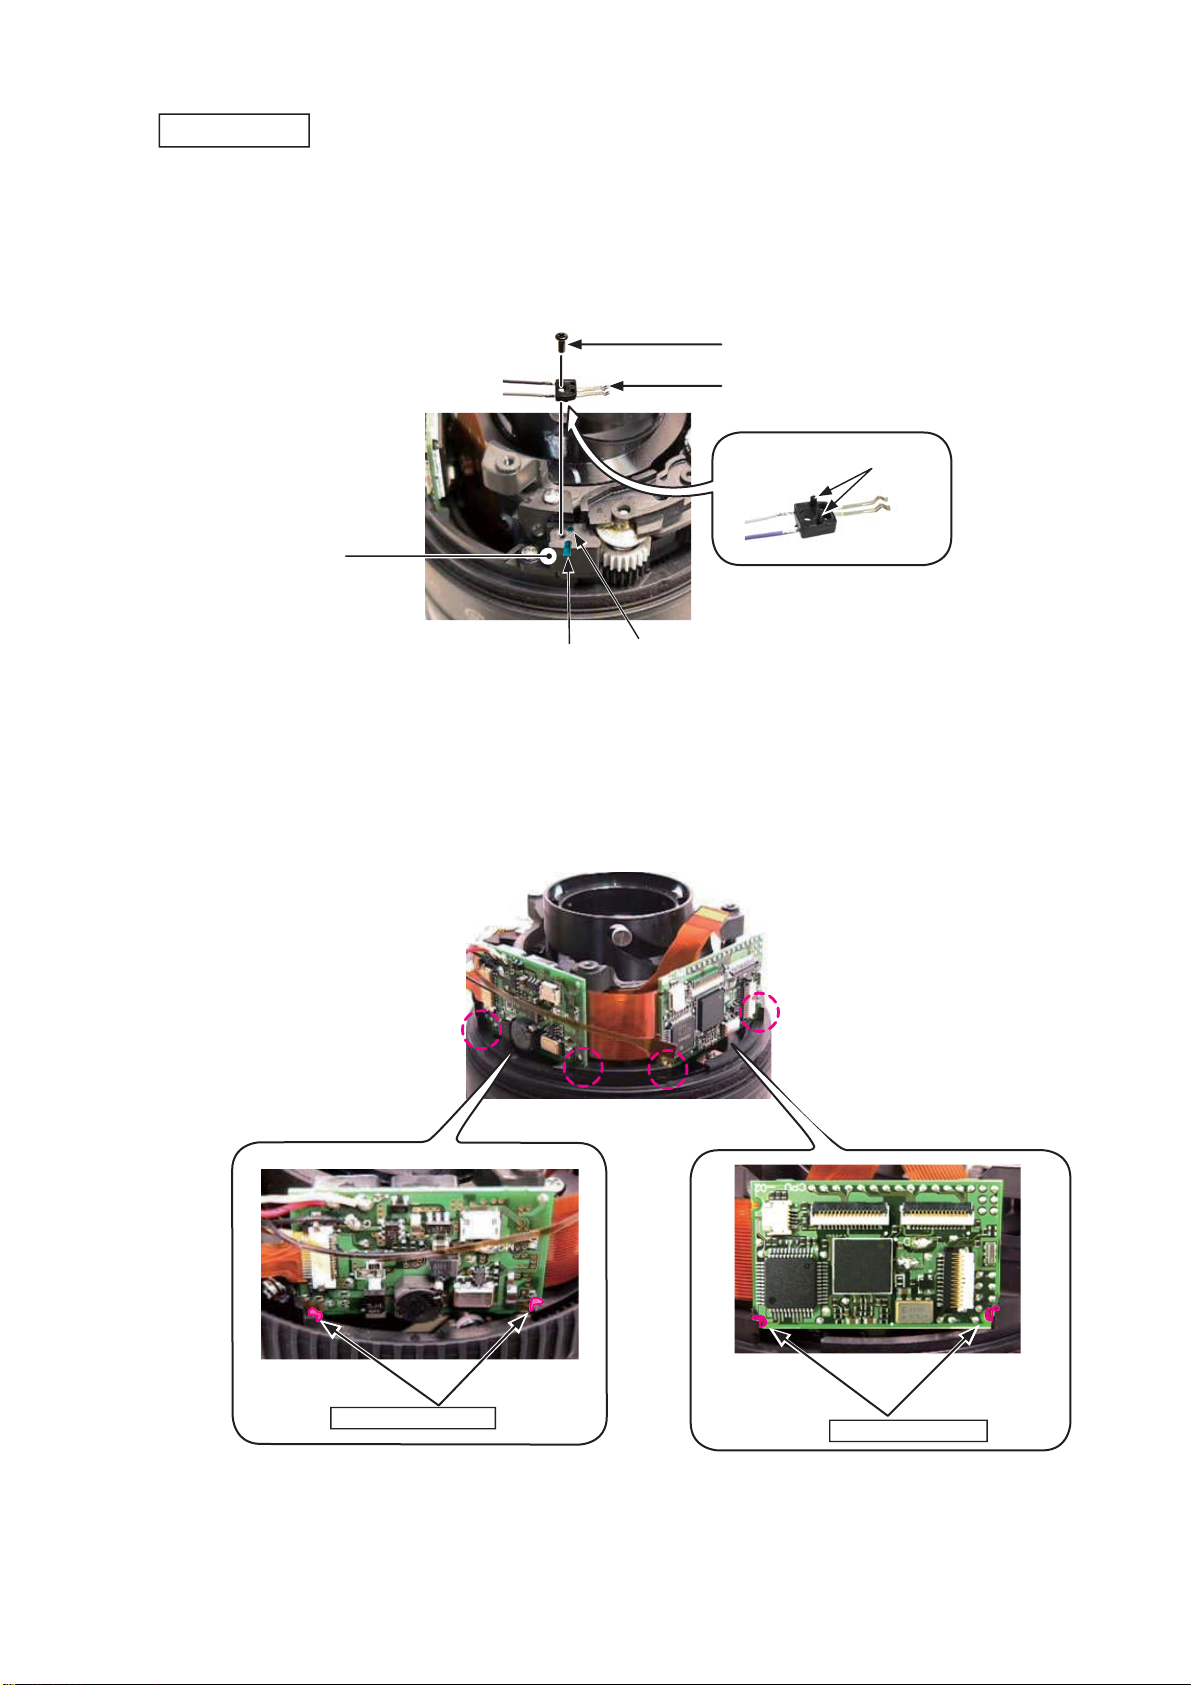
Page 49
JAA80051-R.3741.A
INC
MF brush
Attach the MF brush (B2533) to SWM unit (B501) by fi tting the two bosses of [B2533] in the hole and
・
groove of [B501], and tighten the screw (#587).
#587
B2533
Boss×2
B501
Caution:
Do NOT deform the brush.
・
Groove
Hole
Do NOT use a deformed brush.
・
Apply the adhesive to the below locations, and fi x the main PCB (#1001).
・
Adhesive: SX720B
- A27・AF-S DX 16-85/3.5-5.6G VR -
Adhesive: SX720B
Page 50
JAA80051-R.3741.A
INC
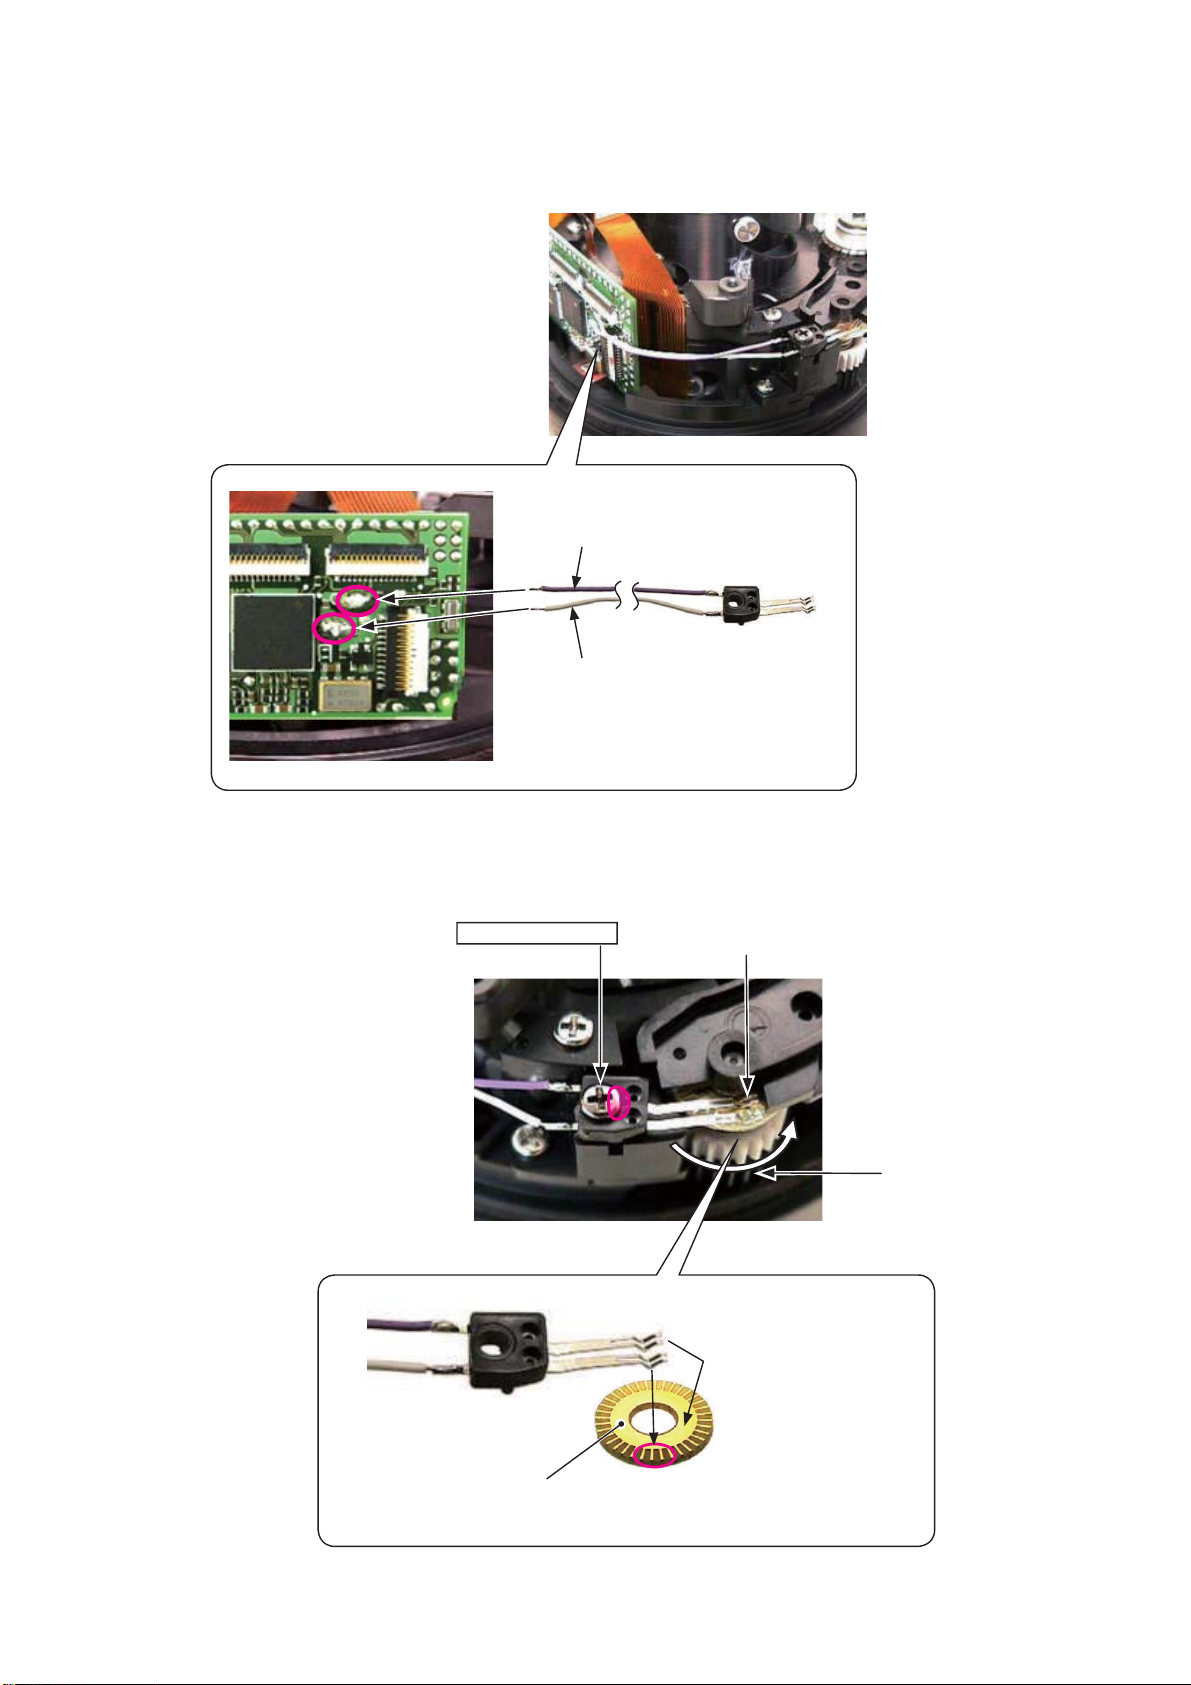
Solder the lead wire (pink: #1025) of MF brush (B2533) and the lead wire (white: #1026) on the main PCB
・
(#1001).
#1025
#1026
Turn MF gear (#535) and confi rm the contacting condition between MF brush (B2533) and M/A-PCB
・
(#1012).
Apply the adhesive to the head of the screw (#587) to fi x.
・
Adhesive: Screwlock
#587
#535
Check whether to contact
M/A-PCB.
#1012
- A28・AF-S DX 16-85/3.5-5.6G VR -
Check whether to contact the pattern
surface of M/A-PCB.
Page 51
MF ring
INC
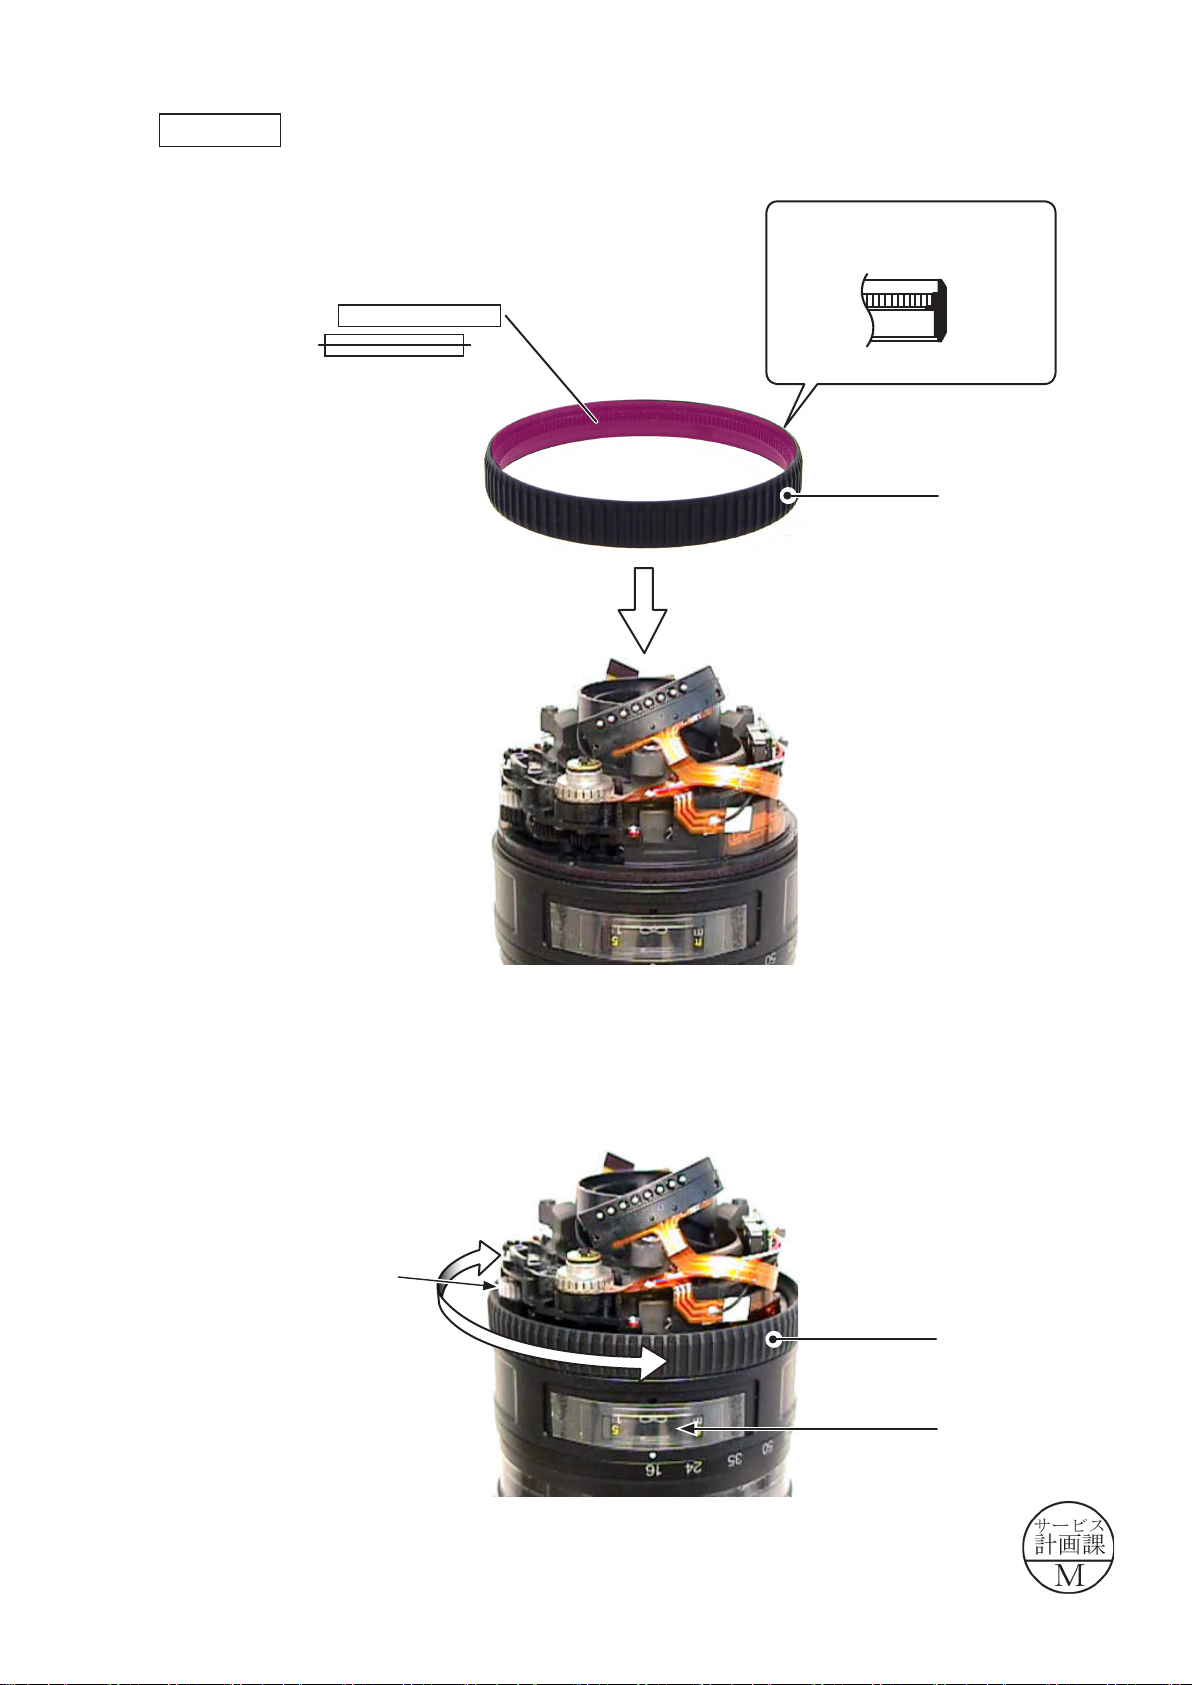
Mount MF ring (#26).
・
△ (Revision)
Grease: MZ-400EL
Grease: MZ-400T
Apply to the overall
inner surface.
JAA80051-R.3741.A
Be careful of up/downward
direction for mounting.
Cross-section view of [#26]
#26
Turn MF ring (#26) and check whether MF gear (#535) and gear unit (B40) move subsequently.
・
#535
Changed page △× 1
- ・AF-S DX 6-85/3.5-5.6G VR -
#26
B40
March�3�008�3�0083�008�008008
Page 52
JAA80051-R.3741.A
INC
GMR FPC
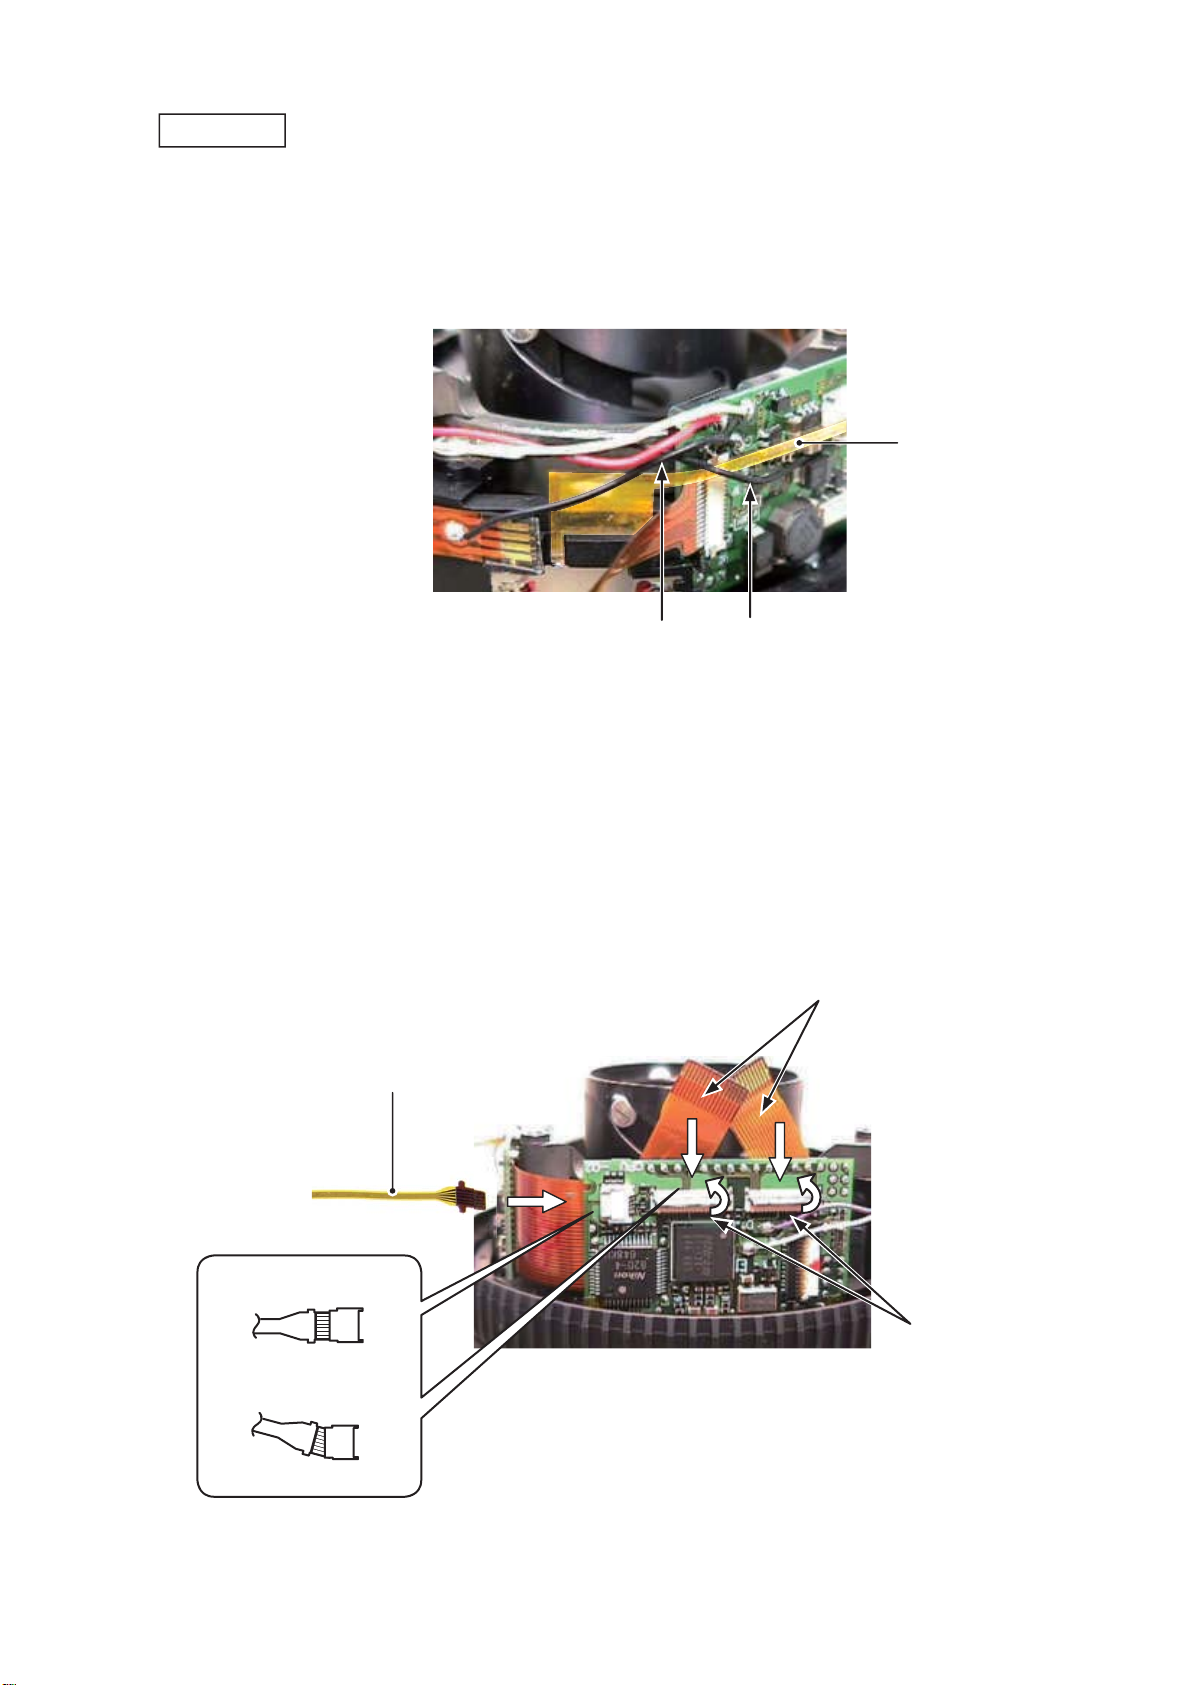
Pass the GMR-FPC (#1011) under the lead wire (#1027) of the lug plate unit and the lead wire (#1031) of
・
SMW-FPC.
#1011
#1031
Connect the GMR-FPC (#1011) to the connector of the main PCB.
・
Connect the connection-FPCs (#1008) to the connectors of the main PCB.
・
Caution: After connecting the connection-FPCs (#1008), be sure to lock the connectors.
#1011
#1027
#1008
Insert FPC all the way
seated in.
Lock here.
Do NOT insert FPC
sideways.
- A30・AF-S DX 16-85/3.5-5.6G VR -
Page 53
JAA80051-R.3741.A
INC
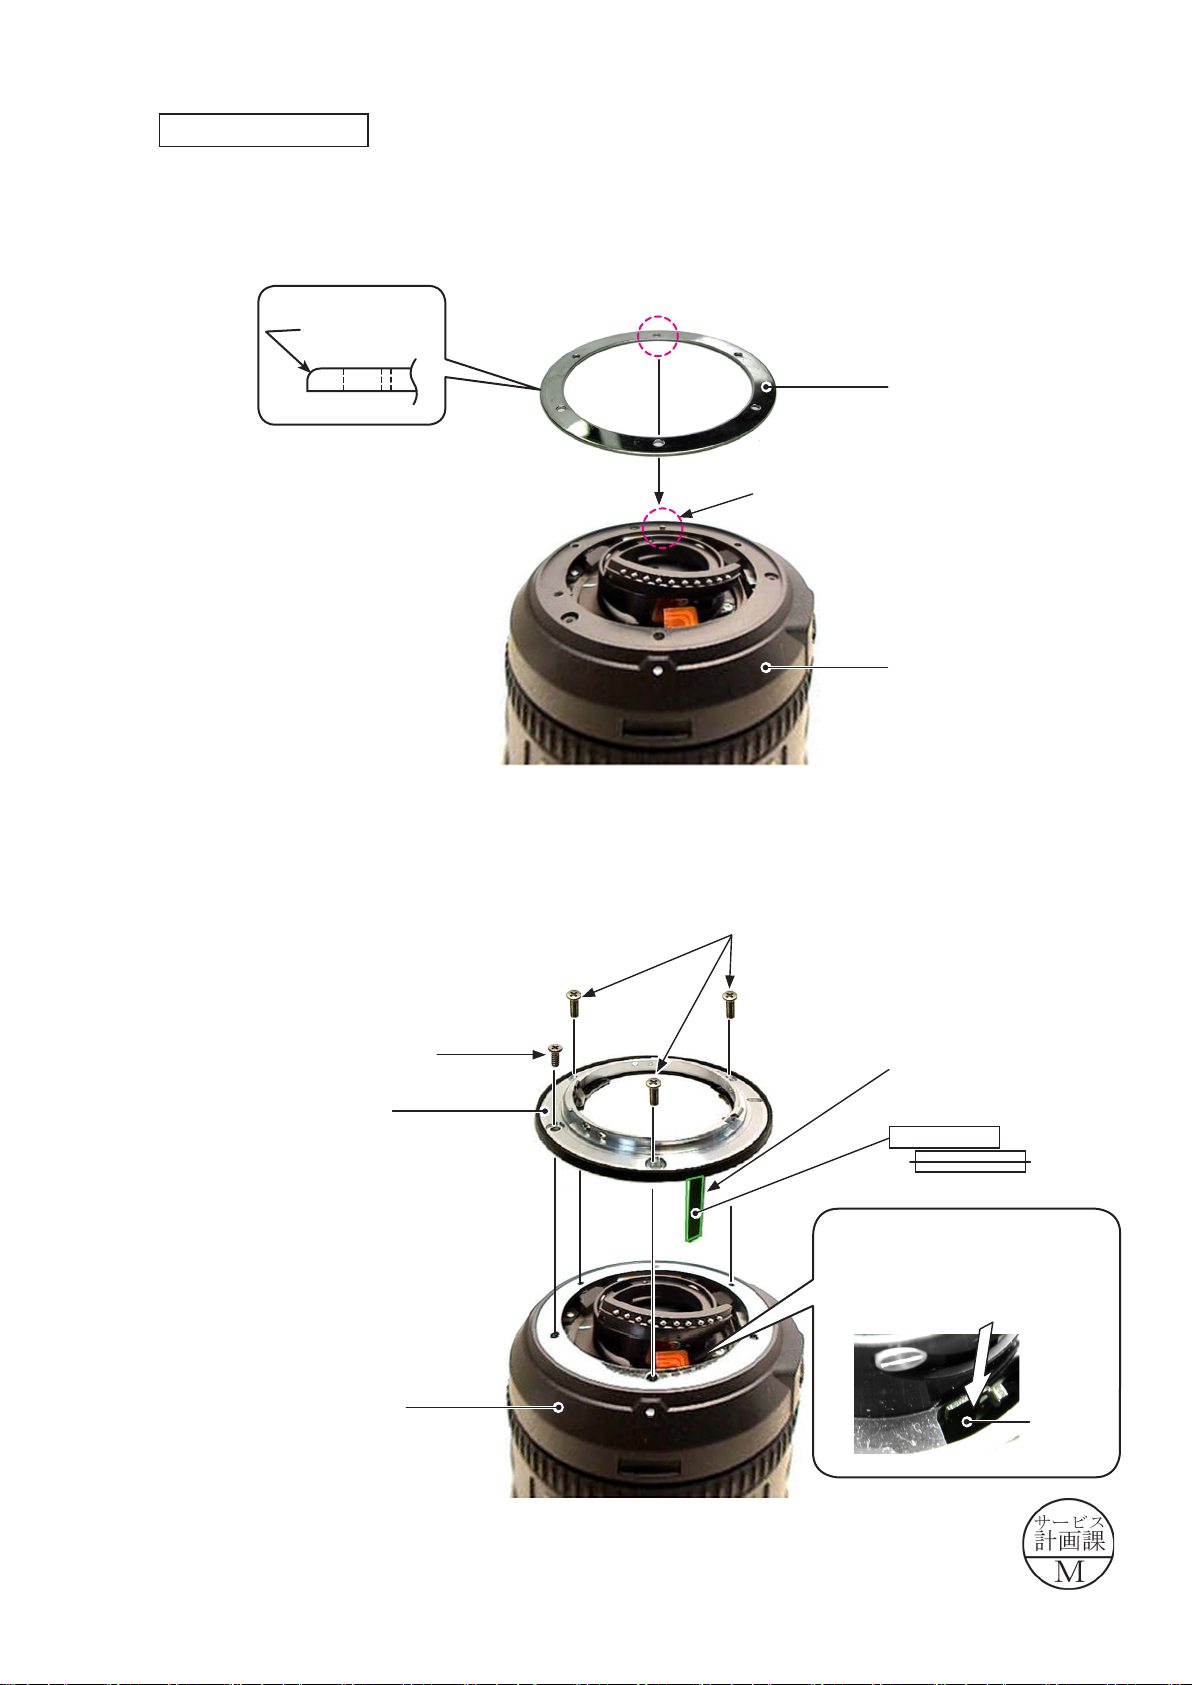
Check conduction between the white screw hole of the fi xed tube (#50) and the screw (#123) that attaches
・
the lug plate unit (B1028).
Apply the head of the three screws (#123) to fi x.
・
Adhesive: Screwlock
White screw hole of [#50]
Do NOT touch "A" area.
"A" area
Check conduction
Value read by tester - Internal resistance value<0.5Ω
#123
Adhesive: Screwlock
#123×2
Fixed ring unit
Connect the FPC of the fi xed ring to the connector of the main PCB (B1001).
・
Mount the fi xed ring unit (B29) on MF ring (#26).
・
B29
#26
Insert FPC all the way
seated in.
Do NOT insert FPC
sideways.
- A31・AF-S DX 16-85/3.5-5.6G VR -
Page 54
Bayonet mount unit
INC
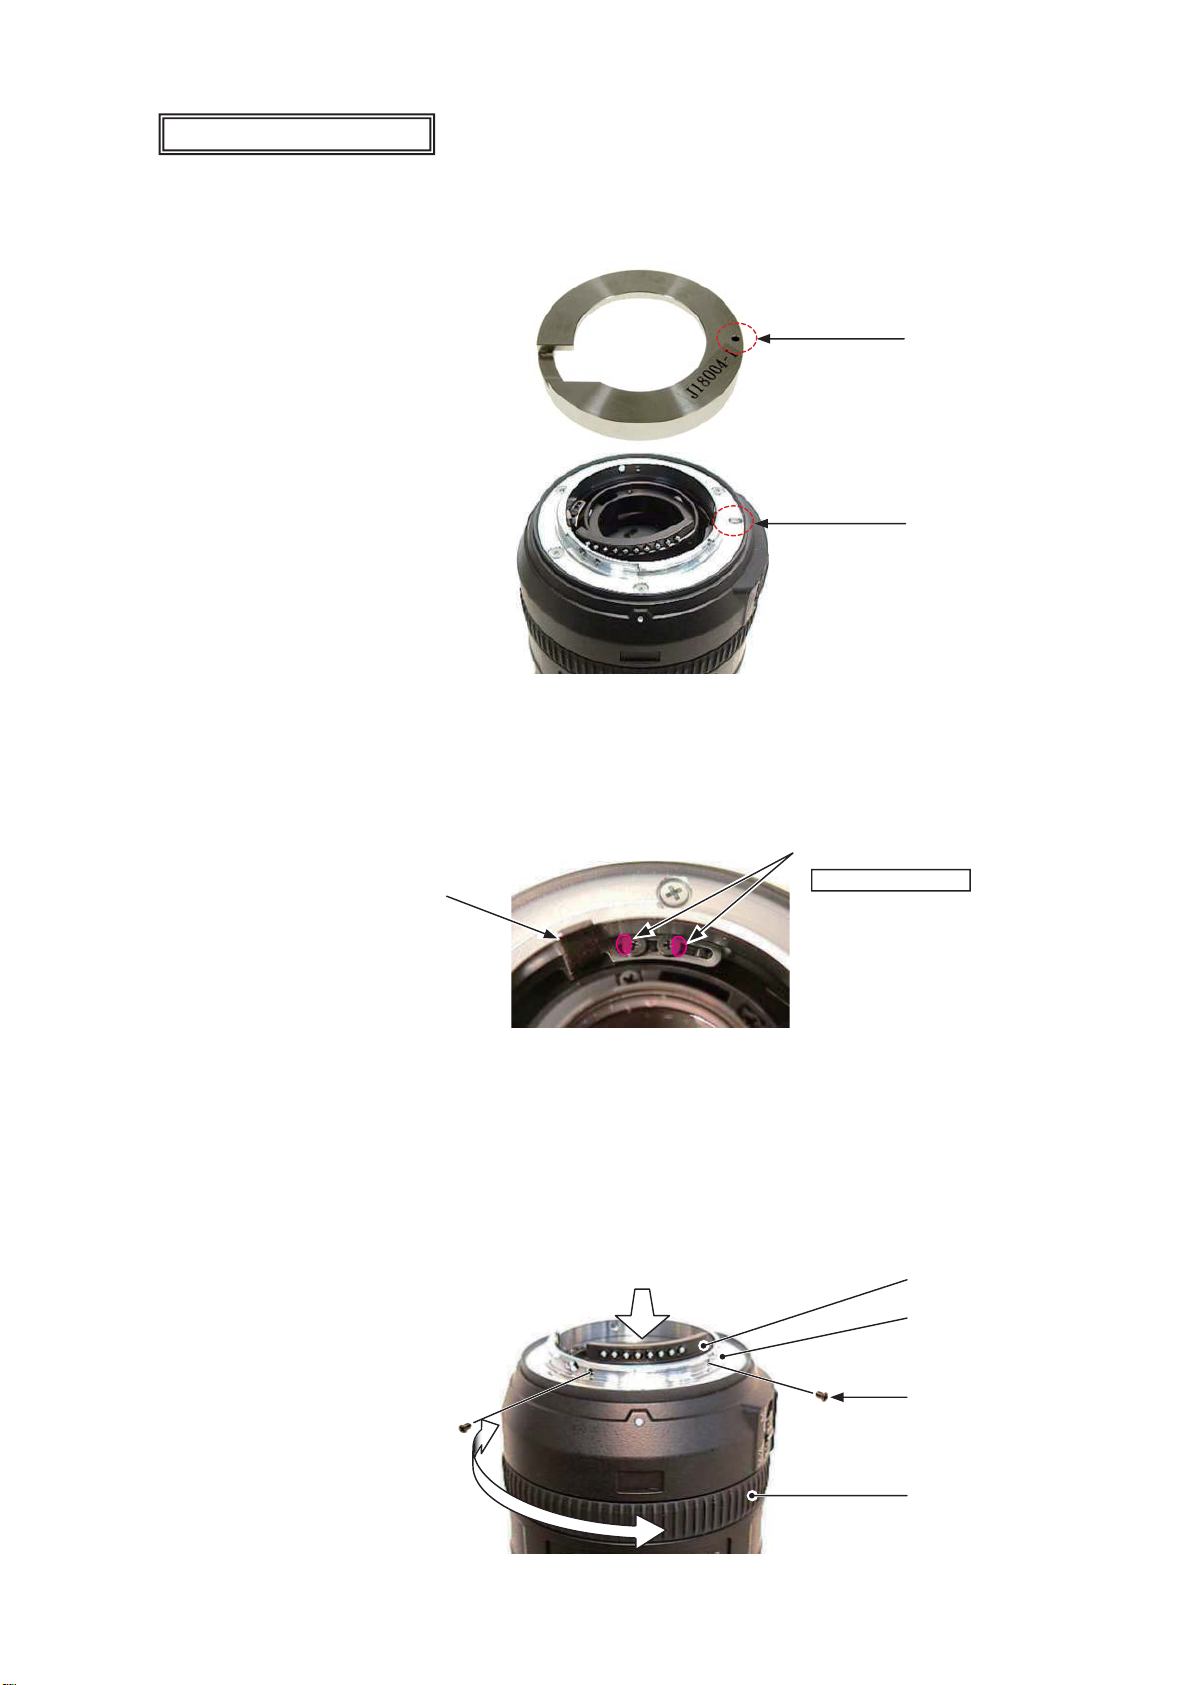
Put the washer (#79) on the rear cover unit (B29) by tting the boss in the hole.
・
If more than one washer is used, put a thicker washer on the other(s).
・
Shear-drooped
side upward
Boss
JAA80051-R.3741.A
#79 (A-J)
Mount the bayonet mount unit (B30) on the rear cover unit (B29).
・
Tighten the three screws (#115) and one screw (#114).
・
#114
B30
B29
#115×3
#61
△ (Revision)
Grease: I-40
Grease: G8240
Apply to the overall surface.
Insert the lever(#61) section’s head
into the cutout of the blade actuating
plate (#33) to assemble.
Changed page △× 1
B29
- 3・AF-S DX 6-85/3.5-5.6G VR -
#33
March�3�008�3�0083�008�008008
Page 55
JAA80051-R.3741.A
INC
Aperture lever adjustment
Set the zoom ring to TELE-end.
When the lock pin of [J18004-1] is put into the lock hole of the bayonet, confi rm that the aperture blades
become fully open.
J18004-1
Lock pin
Lock hole
If the aperture blades open quickly or slowly, adjust the position of the aperture lever with the two screws
(#121).
When the position of the aperture lever is adjusted, apply the adhesive to the head of the two screws (#121)
・
to fi x.
#121×2
Aperture lever
Set the zoom ring to TELE.
Place the contact unit (B1007) on the bayonet mount unit (B30) by pressing in the direction (clockwise)
for positioning.
Tighten the two screws (#117).
Turn MF ring (#26) and check operations.
Caution: Contact unit (B1007) must not be tilted,
slackened, nor gapped from the bayonet mount
(B30).
Adhesive: Screwlock
B1007
B30
#117×2
#26
- A33・AF-S DX 16-85/3.5-5.6G VR -
Page 56
JAA80051-R.3741.A
INC
4th lens group unit
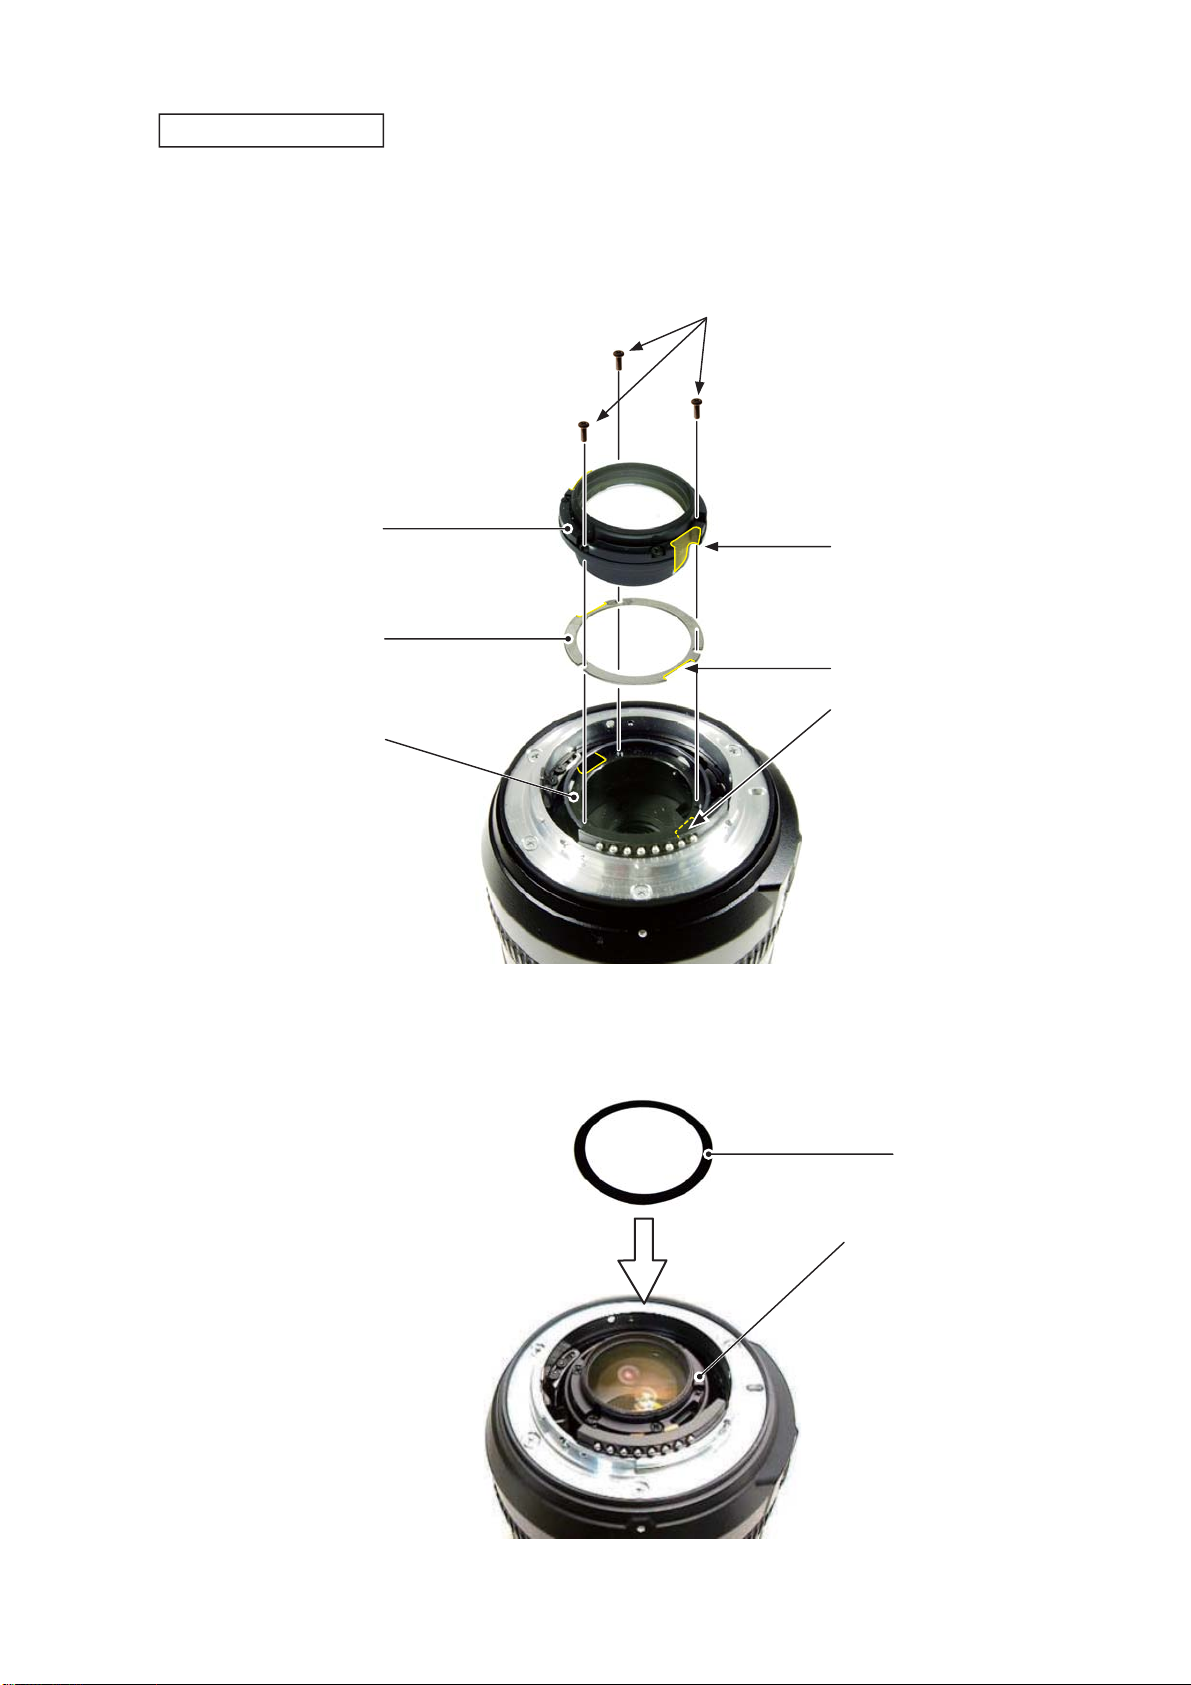
Mount the 4th lens-G unit (B2046) by fi tting in the cutouts two each of the washer (#139) and the 4th lens-G
・
sliding ring (#48).
Secure the 4th lens-G unit (B2046) with the three screws (#124).
・
Note that when the 4th lens group is removed, lens alignment work will be necessary.
・
#124×3
B2046
#139
#48
Adhere the sheet (#70) on the 4th lens-G unit (B2046).
・
Cutout×2
Cutout×2
Cutout×2
#70
B2046
- A34・AF-S DX 16-85/3.5-5.6G VR -
Page 57
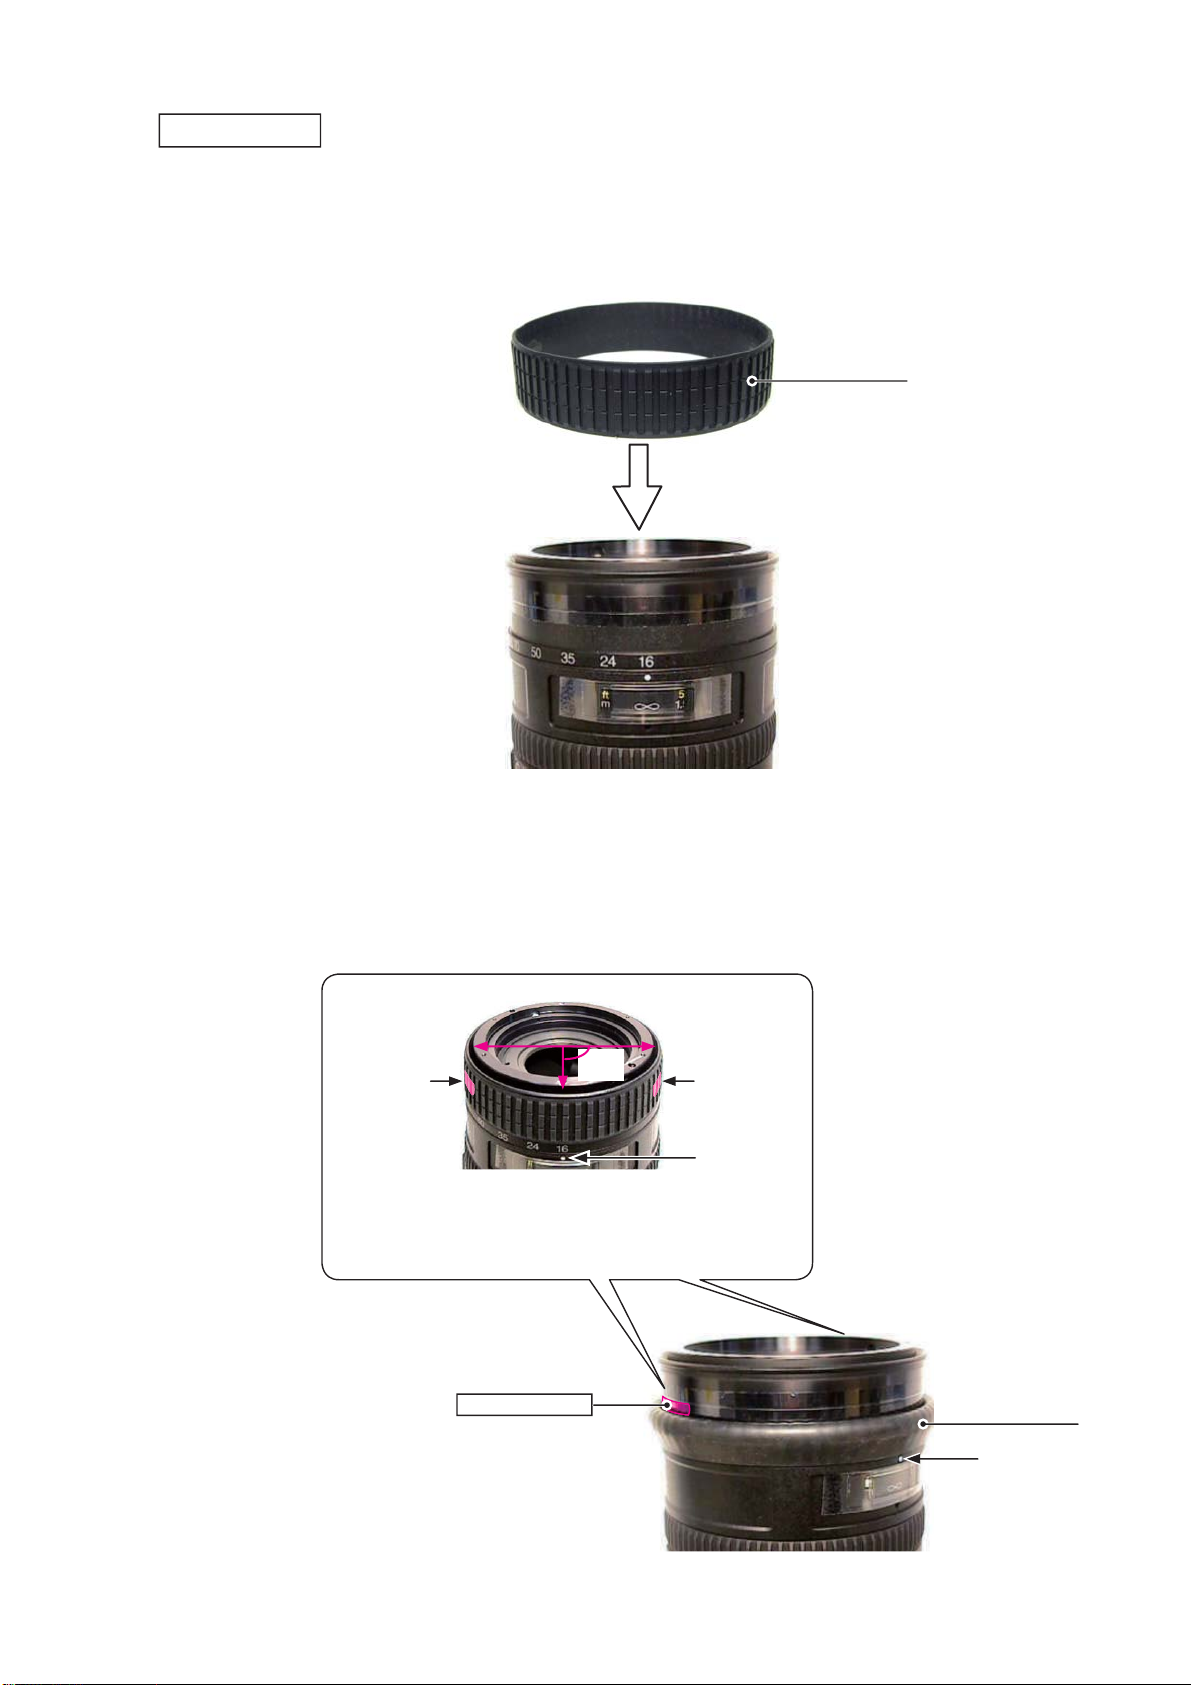
Rubber ring
INC
Mount the rubber ring (#37).
・
JAA80051-R.3741.A
#37
Turn over the rubber ring (#37) and apply the adhesive as below.
・
Adhesive Adhesive
Apply the adhesive to 2 places which are
positioned perpendicular (90°) to the index.
Adhesive: SX720B
90°
Index
#37
Index
- A35・AF-S DX 16-85/3.5-5.6G VR -
Page 58
JAA80051-R.3741.A
INC
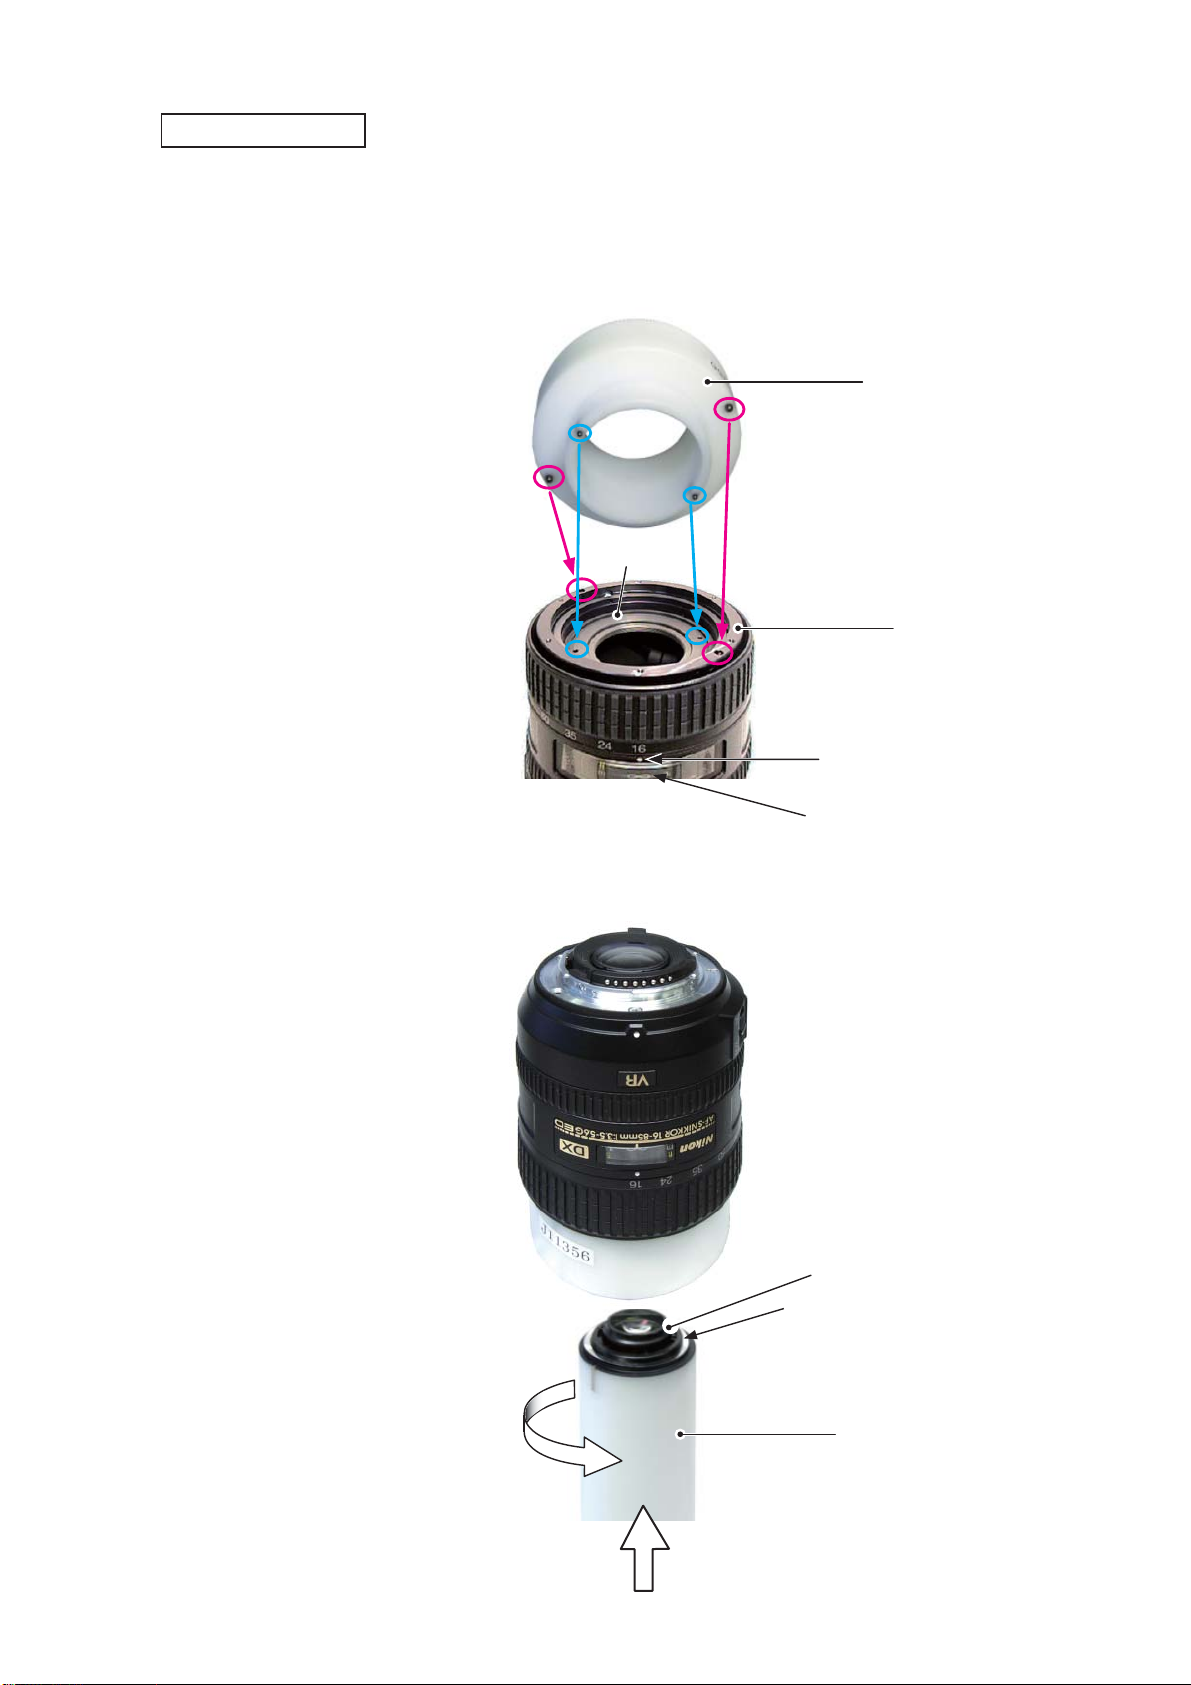
2nd lens group unit
Set the zoom ring to WIDE-end.
・
Align "∞" position of the focus index (#49) with the below index.
・
Mount the fi xing tool for the 2nd lens-G (★J11356) by fi tting its protrusions in the holes of the 1st lens-G
・
cam ring (#38) and the 2nd lens-G cam ring (#25).
J11356
★
#25
#38
Index
#49
Turn clockwise the wrench for the 2nd lens-G (★11358), into which the 2nd lens-G unit (B2043) and the
・
washer (#80) are assembled, and fi x them into the 2nd lens-G cam ring (#25).
B2043
#80
- A36・AF-S DX 16-85/3.5-5.6G VR -
J11358
★
Page 59
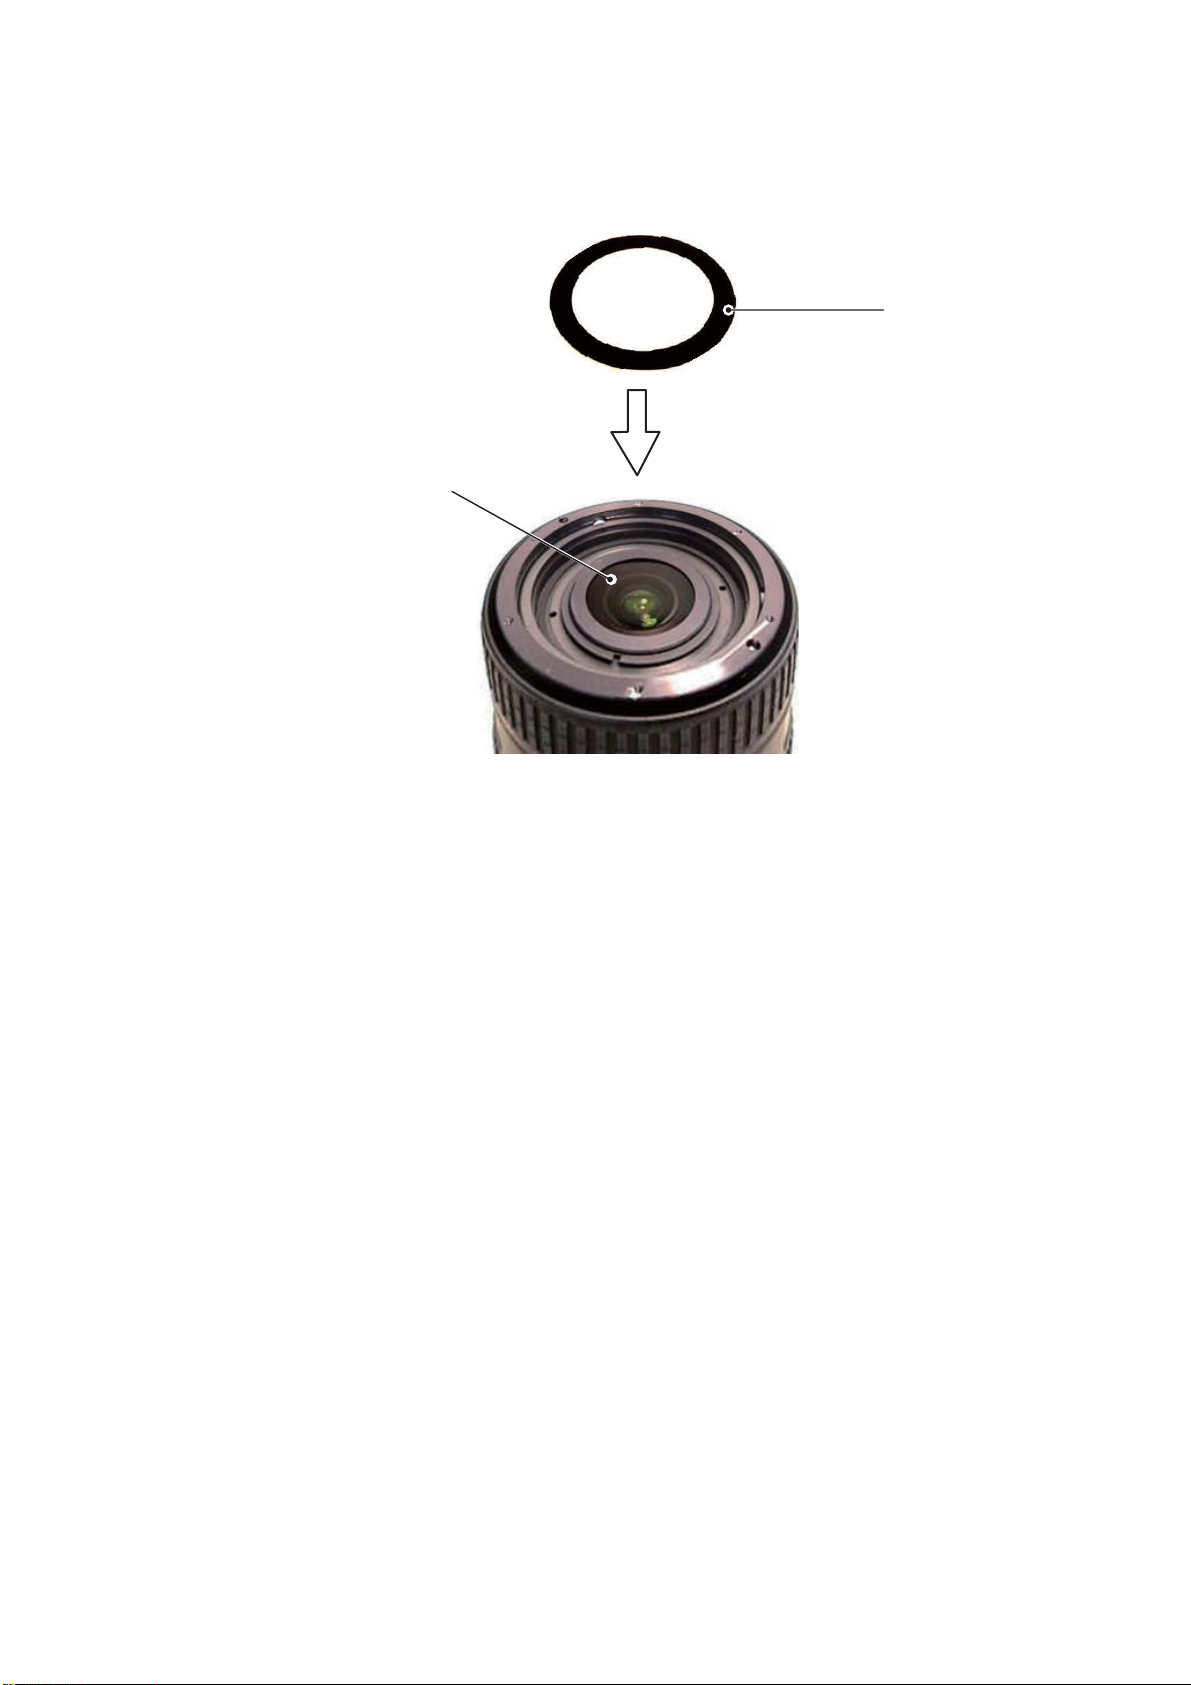
Set the zoom ring to WIDE, and adhere the sheet (#62).
INC
・
B2043
JAA80051-R.3741.A
#62
NOTE:
If dust/dirt is attached to the lens surface of the 2nd lens-G(B2043), blow them away with a
blower as much as possible.
If impossible, dip a wiping cloth (Savina Minimax) a little in ethanol, and wipe the surface
lightly.
- A37・AF-S DX 16-85/3.5-5.6G VR -
Page 60
JAA80051-R.3741.A
INC
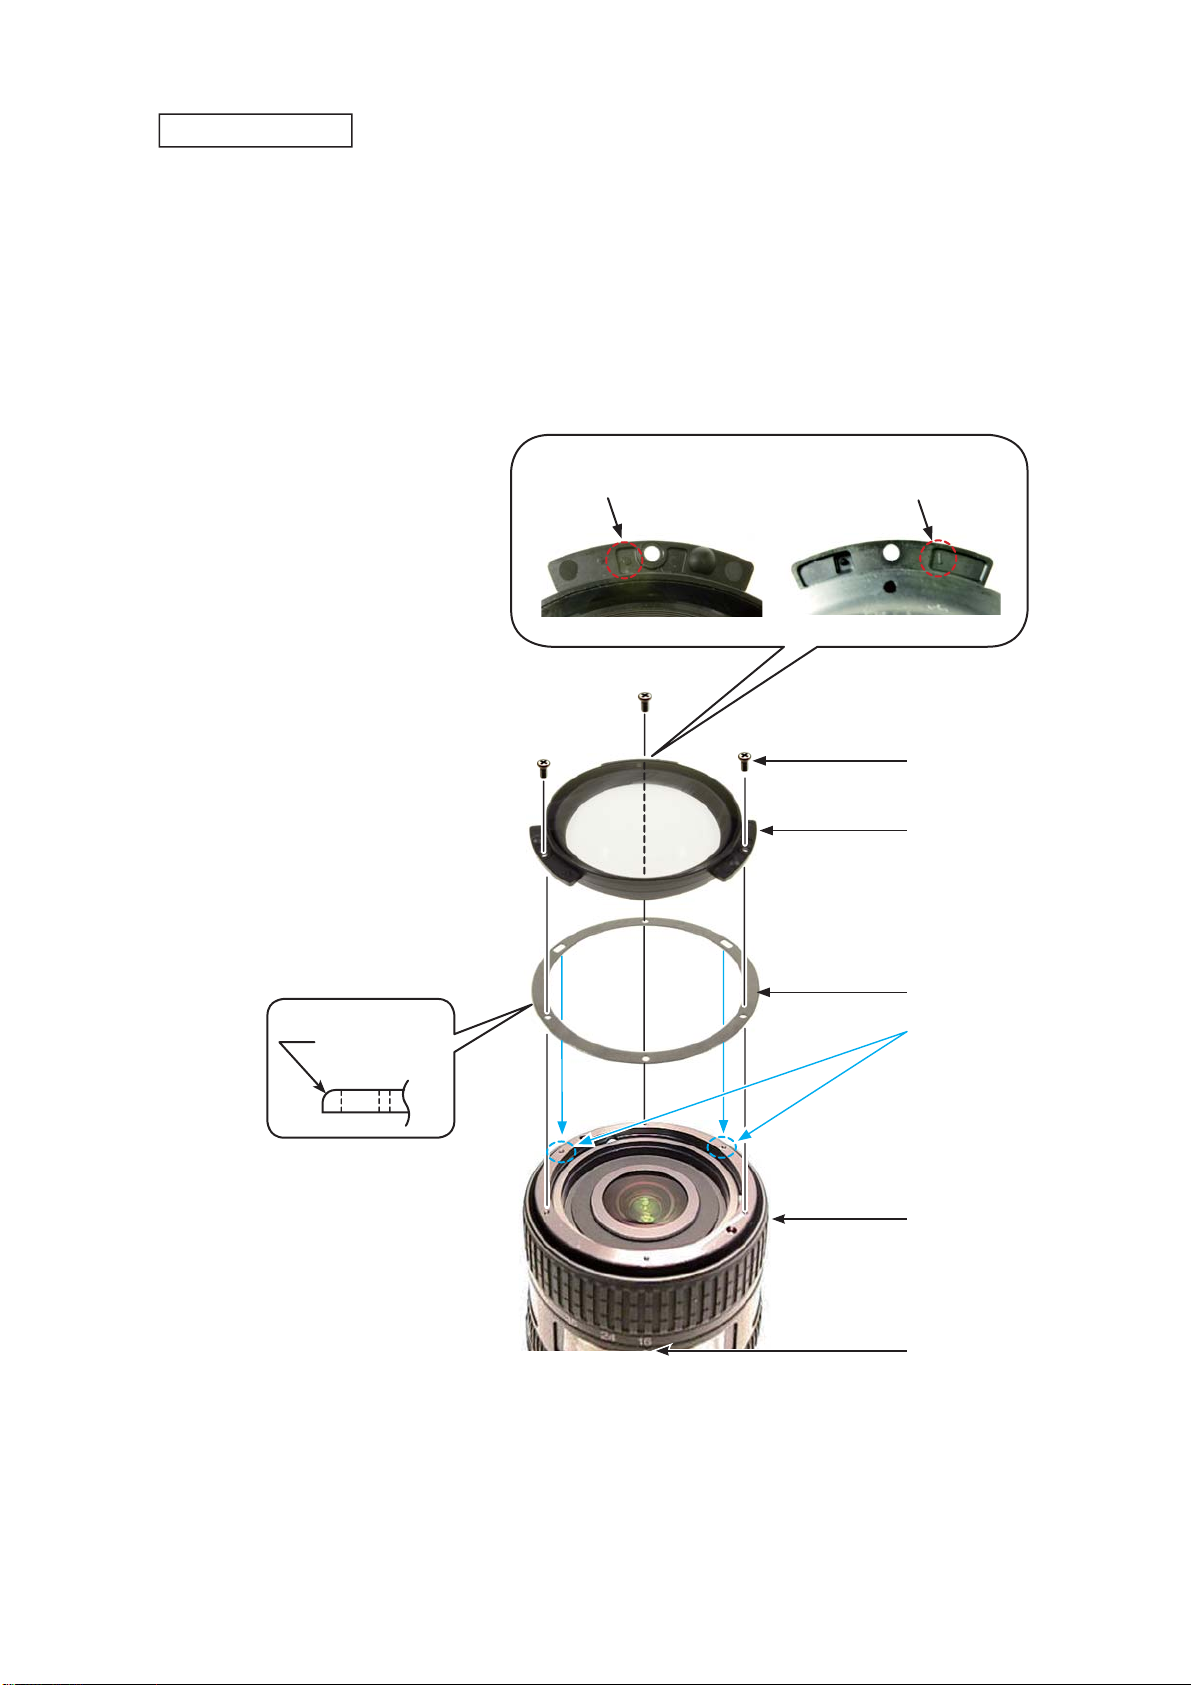
1st lens group unit
Set the zoom ring to WIDE.
・
Mount the 1st lens-G unit (B204) by placing the boss ("Mold cavity no.) halfway around from the index.
・
Secure the 1st lens-G unit (B204) with the three screws (#120) by turning clockwise from the index.
・
Note: When the washer (#133) is put, place a thin washer between thick washers.
Shear-drooped
side upward
Boss faces upwards.
"Mold cavity No." faces
downwards.
#120×3
B204
#133
Slotted hole for
assembly
#62
Index position
- A38・AF-S DX 16-85/3.5-5.6G VR -
Page 61
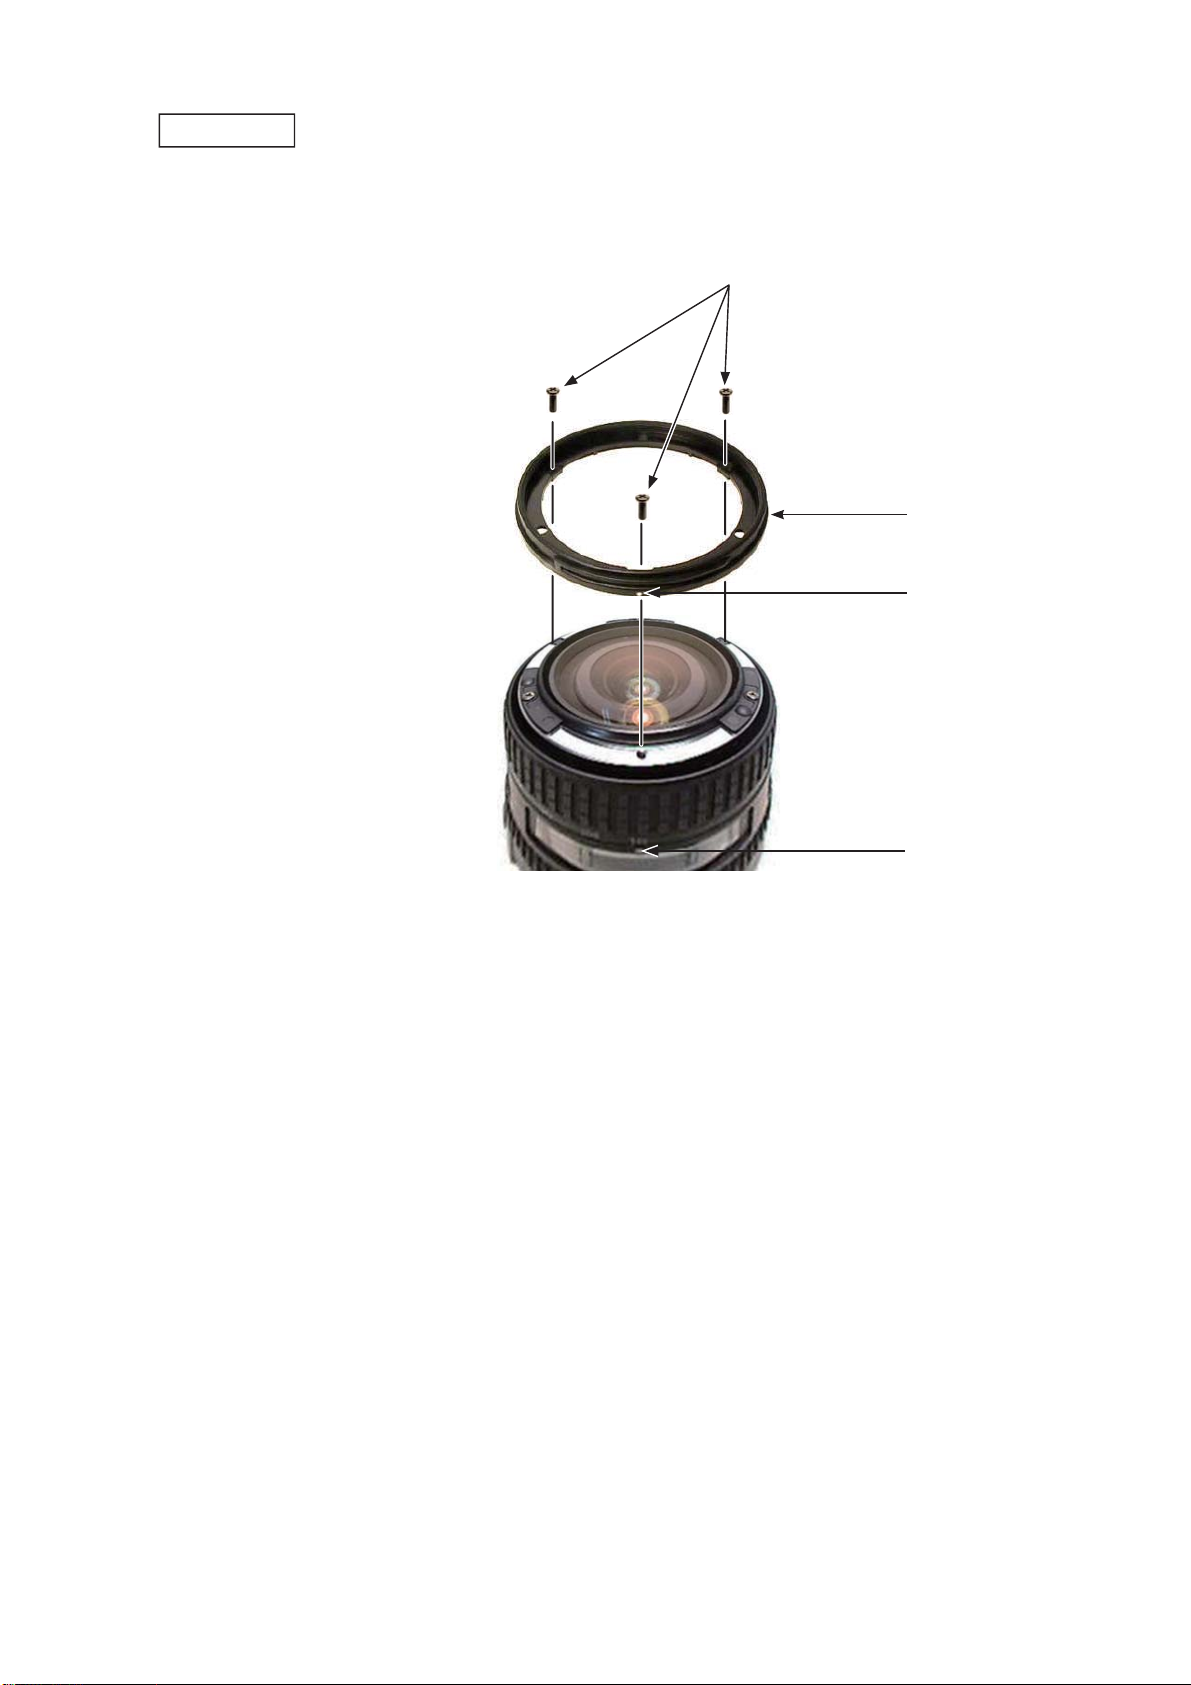
Filter ring
INC
Align the index of the fi lter ring (#35) with the index of the fi xed ring (#55).
Tighten the three screws (#119).
#119×3
JAA80051-R.3741.A
#35
Index
Index of [#55]
- A39・AF-S DX 16-85/3.5-5.6G VR -
Page 62
JAA80051-R.3741.A
INC
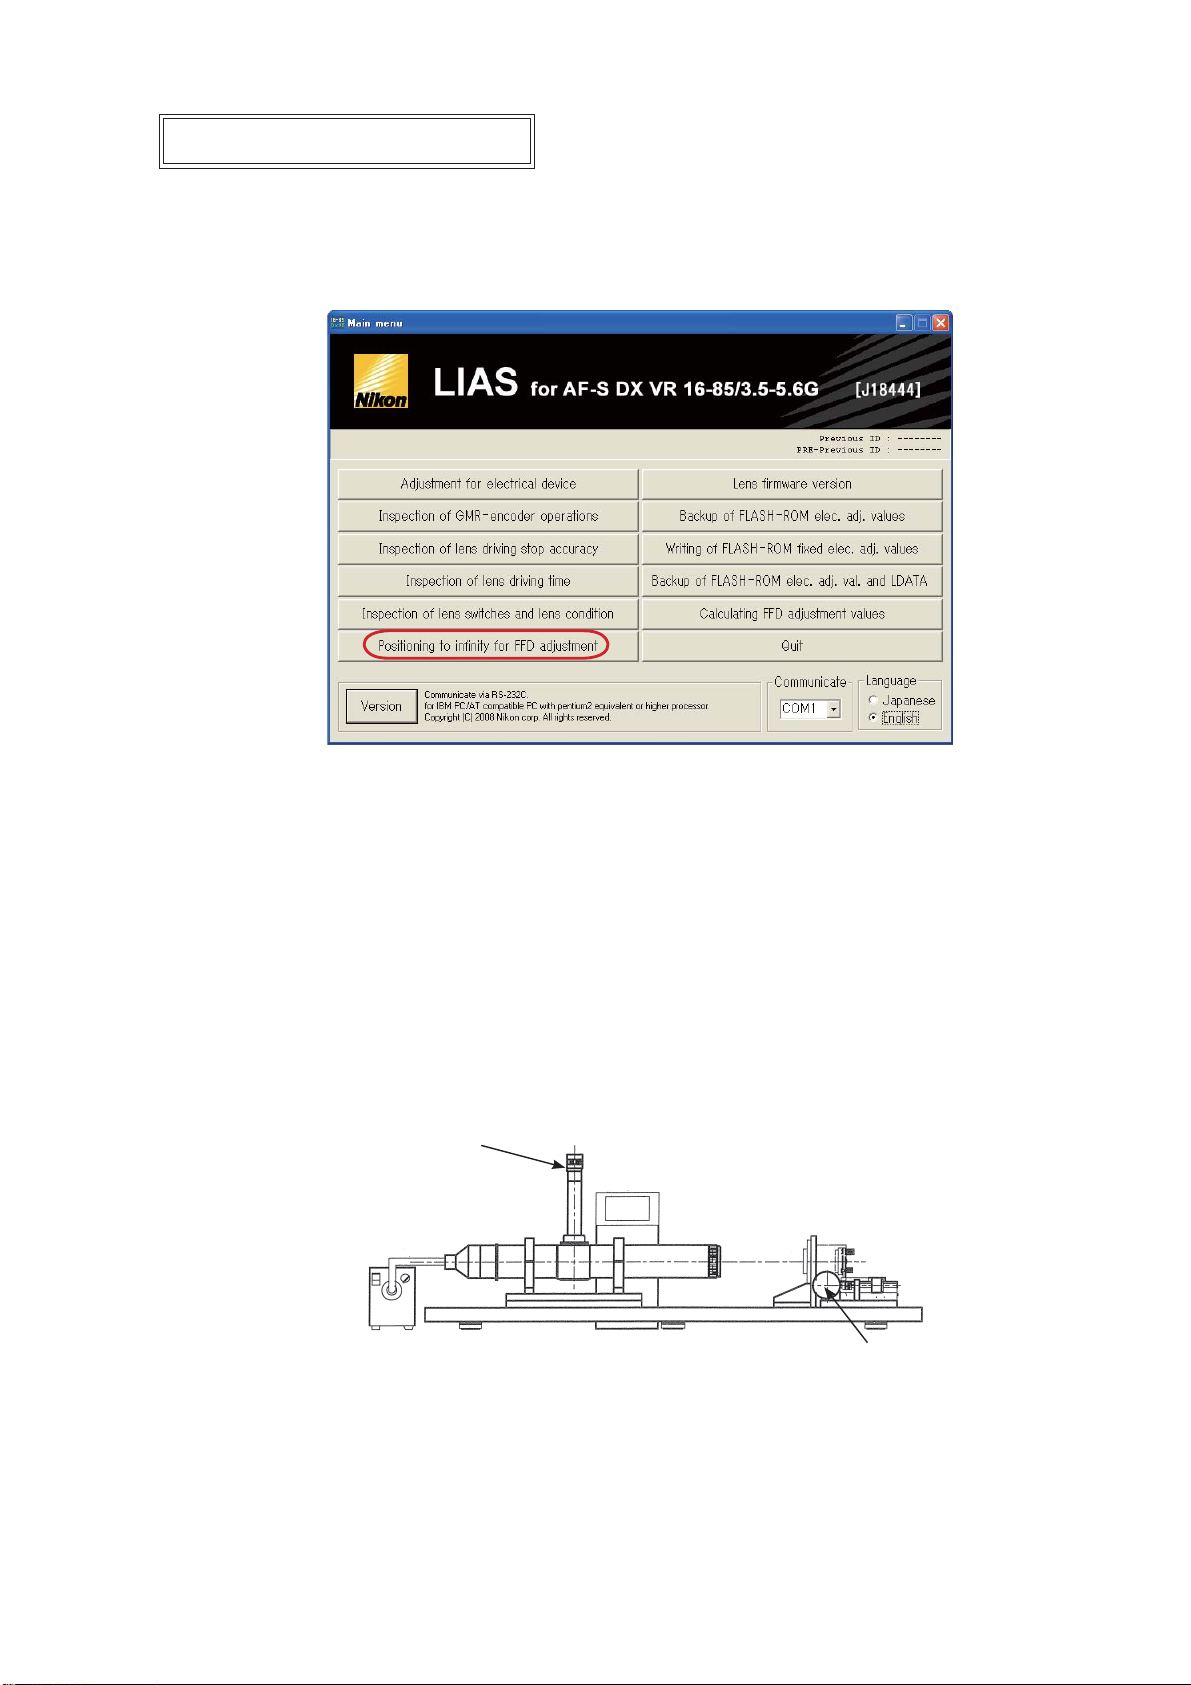
Adjustment of Focus movement (T, W)
★:
Start up the adjustment software (★J18444).
・
Perform "Positioning to infi nity for FFD adjustment" on the main menu for performing "∞" positioning.
・
New tool
Being careful NOT to move the fi lter ring, mount the lens on the horizontal-type collimator.
・
Looking through the eyepiece of the horizontal-type collimator, rotate the mirror micromotion-control
・
handle to adjust focus, then measure focus position at WIDE (16 mm), MIDDLE (35 mm), and TELE
(85 mm).
The focus position to be measured is the numeric number of the boundary line at the moment when the color
of cross lines change from green to orange.
Horizontal-type collimator
<
Eyepiece lens
>
Mirror micromotion-control handle
- A40・AF-S DX 16-85/3.5-5.6G VR -
Page 63
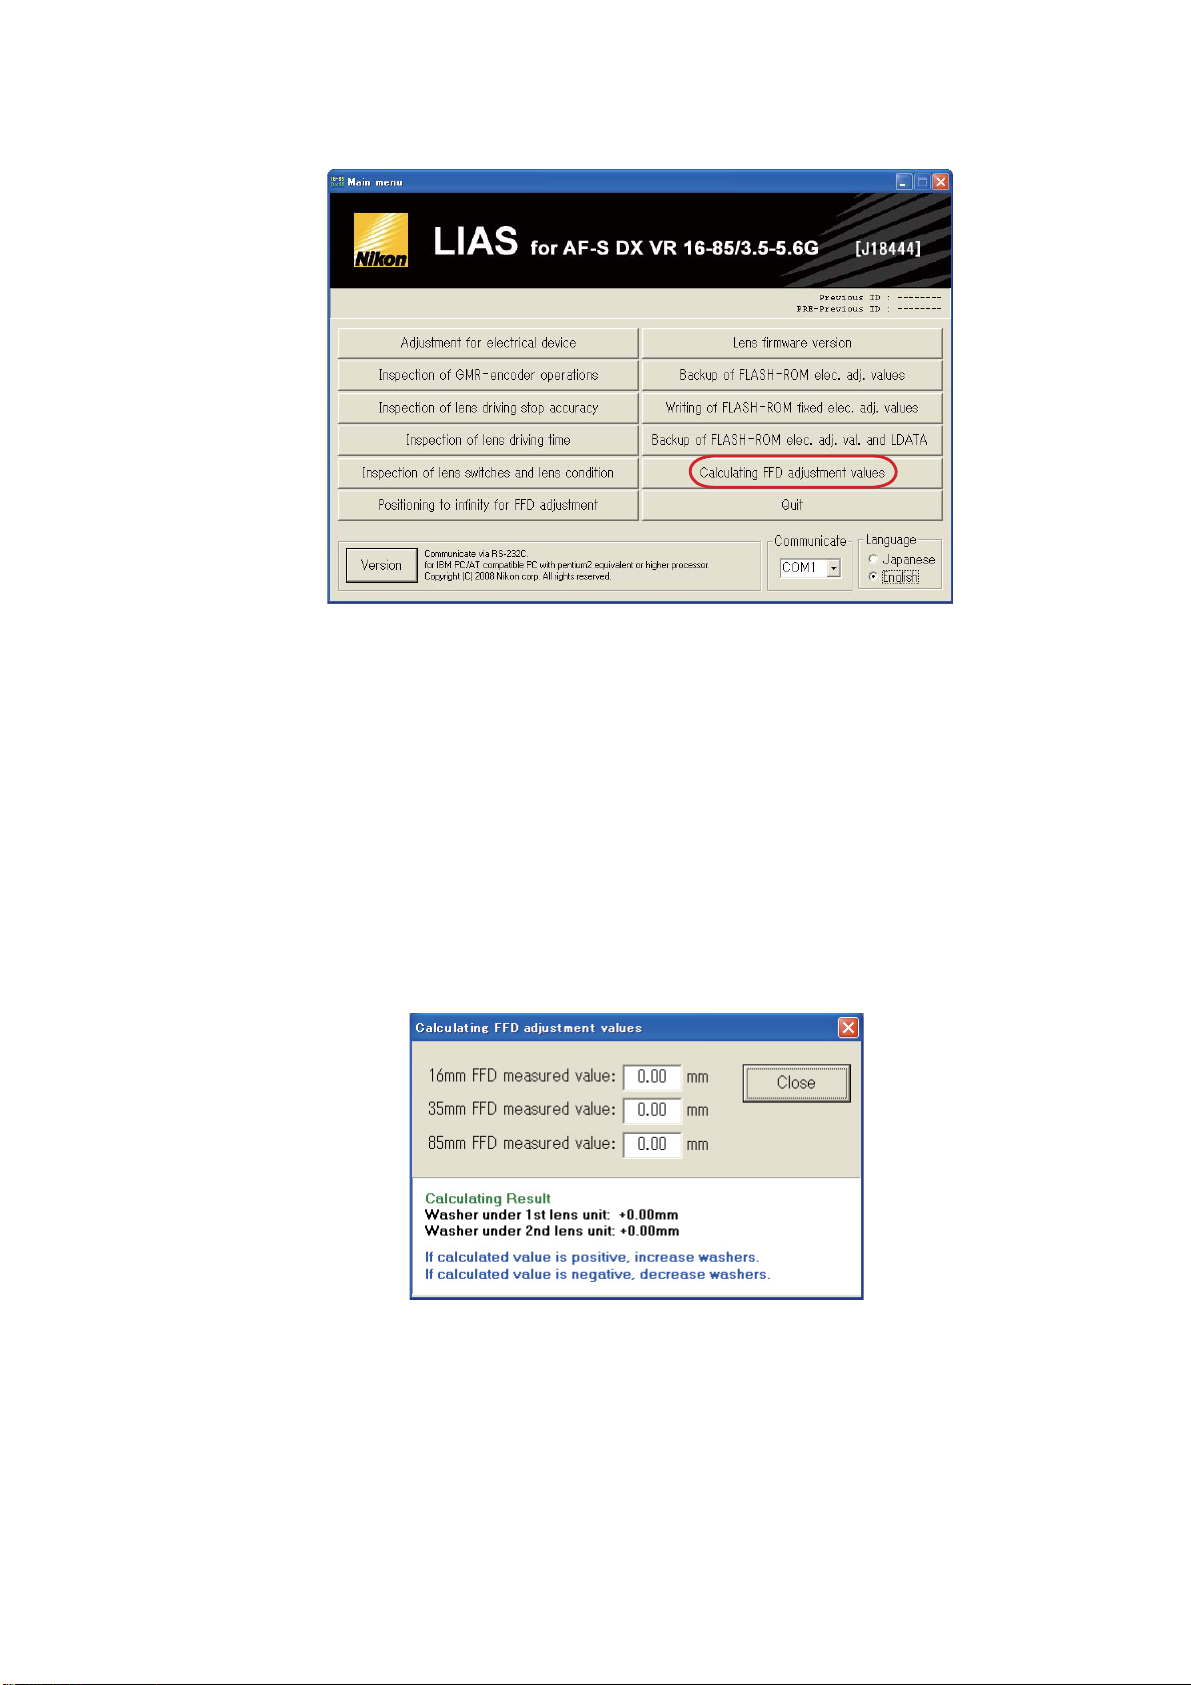
Click "Calculating FFD adjustment values" on the main menu.
INC
・
JAA80051-R.3741.A
Input the focus positions which were measured by the horizontal-type collimator at WIDE (16 mm),
・
MIDDLE (35 mm), and TELE (85 mm) into the below fi elds.
Calculate the adjustment amounts of (1) the washer (#133) which is under the 1st lens group and (2) the
・
washer (#80) which is under the 2nd lens group.
Adjust thickness by increasing/decreasing washers. If the result is positive, increase the thickness, while it
・
is negative, decrease the thickness. (ref. Page A36, A38)
- A41・AF-S DX 16-85/3.5-5.6G VR -
Page 64
JAA80051-R.3741.A
INC
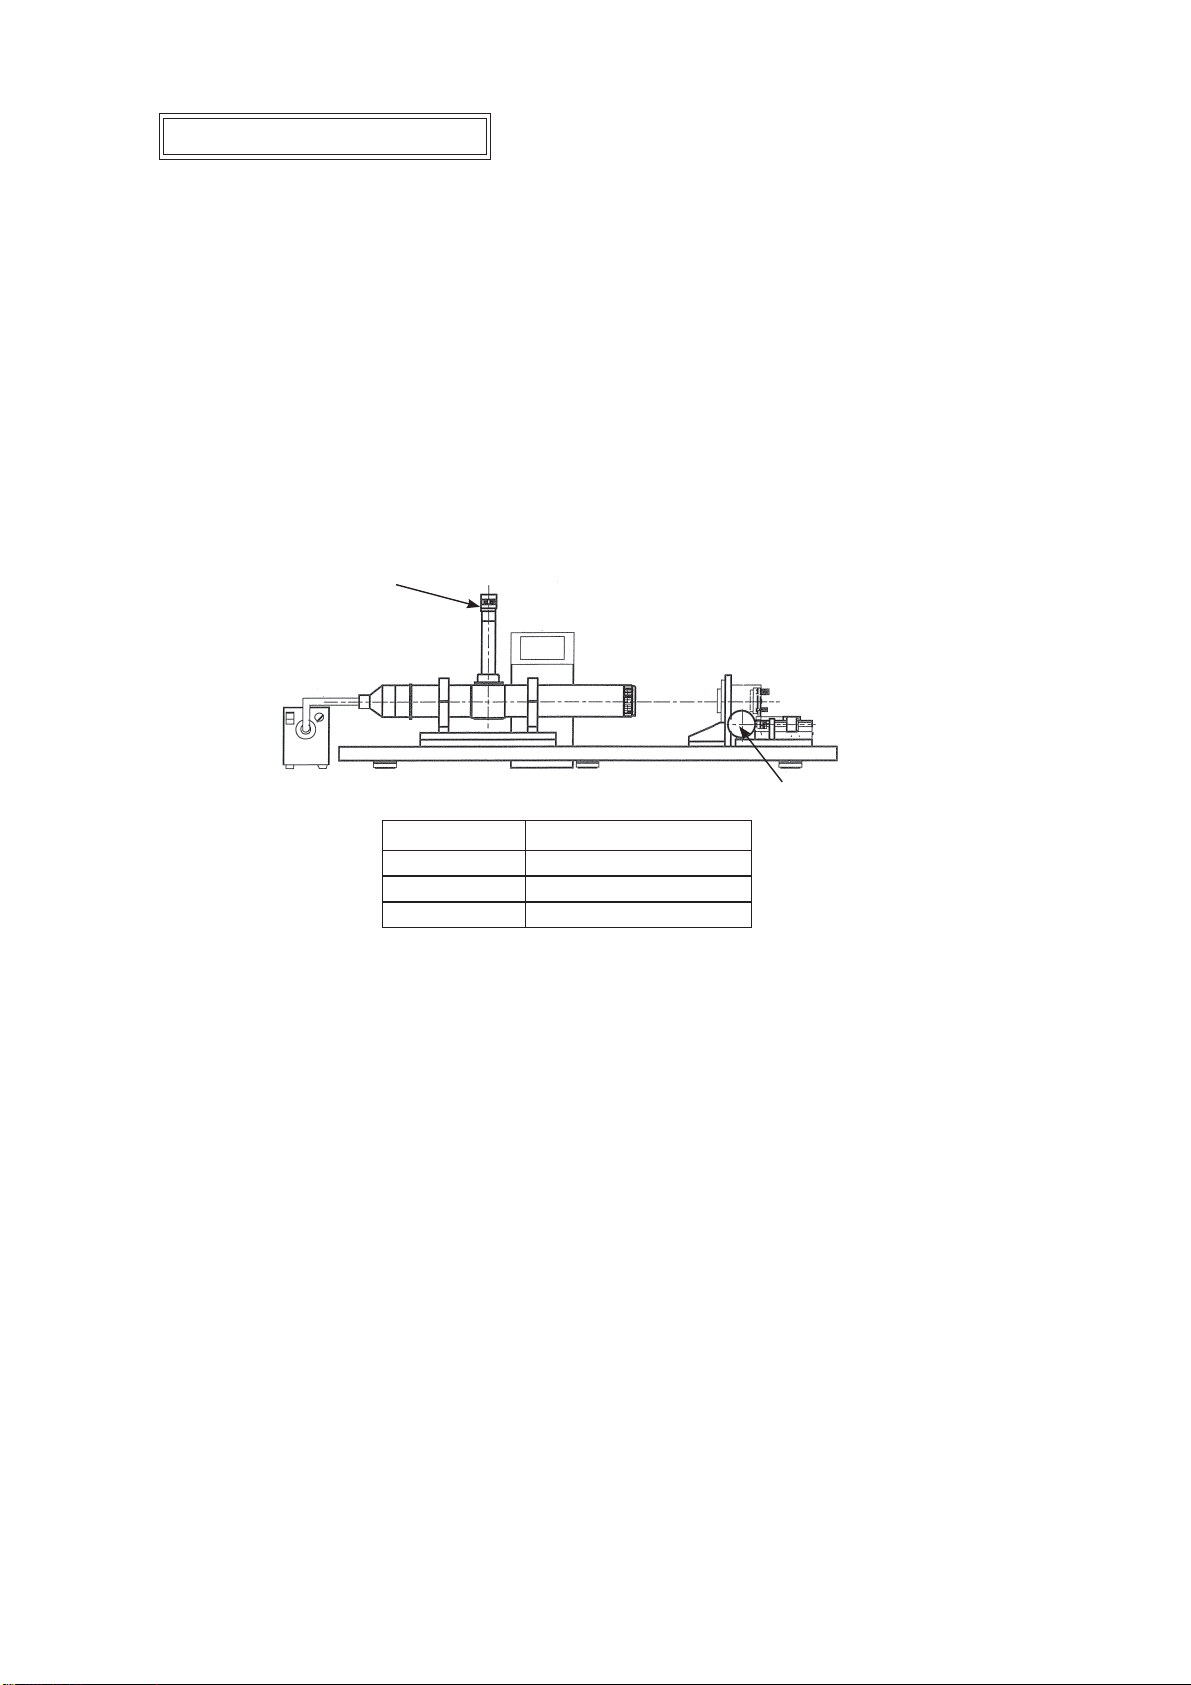
Adjustment of F.F.D (Back focus)
New tool
★:
Start up the adjustment software (★J18444).
・
Perform "Positioning to infi nity for FFD adjustment" on the main menu for performing "∞" positioning.
・
Being careful NOT to move the fi lter ring, mount the lens on the horizontal-type collimator.
・
Looking through the eyepiece of the horizontal-type collimator, rotate the mirror micromotion-control
・
handle to adjust focus, then measure focus position at WIDE or TELE.
The focus position to be measured is the numeric number of the boundary line at the moment when the color
of cross lines change from green to orange.
In case the measured value is out of standard, follow the below procedure.
Horizontal-type collimator
<
Eyepiece lens
>
Mirror micromotion-control handle
Focal length (f) Standard (mm)
16
mm
35
mm
85
mm
Remove the bayonet mount unit (B30).
・
Adjust thickness by increasing/decreasing washers (#79) by a difference from the standard value.
・
0.01~+0.19
0.01~+0.19
-0.09~+0.21
If the difference is positive, increase the thickness, while it is negative, decrease the thickness. (ref. Page
A32).
- A42・AF-S DX 16-85/3.5-5.6G VR -
Page 65
JAA80051-R.3741.A
INC
Lens Alignment
Caution: This adjustment is required when the 4th lens group is removed.
(1) Preparation of Lens optical alignment equipment
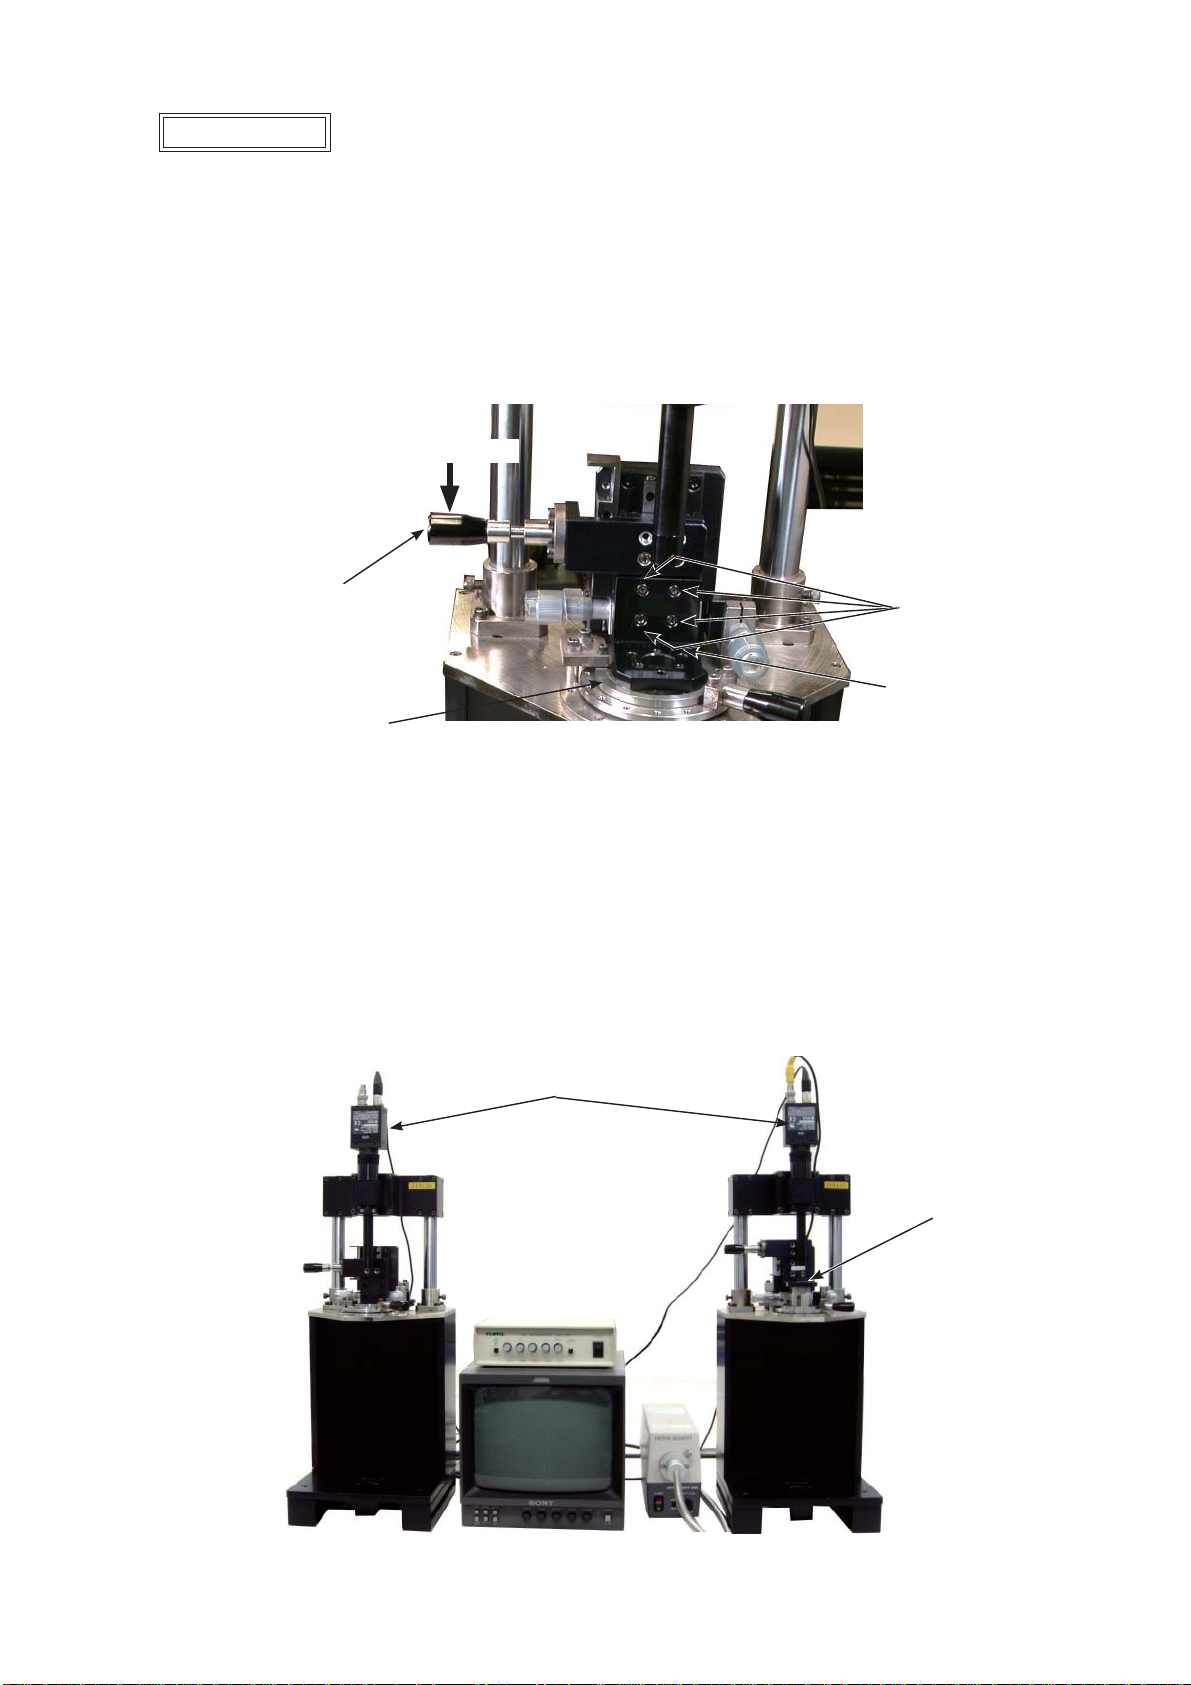
Fix the attachment holder of the rear lens group (J19127T) on the lens equipment.
・
How to Fix: Move down the holder-moving lever slowly so that the attachment holder of the rear lens group
(J19127T) touches the stage.Then tighten four screws to fi x it.
Move down slowly.
Holder-moving lever
Stage
Create the center positioning tool.
・
Refer to [Create positioning tool of Rear lens-group holder for lens alignment] (Page A57) for
Screw×4
Attachment holder of the rear
lens group (J19127T)
how to create.
Create cardboards with which "Lens alignment chart" and "Viewers" are fi t.
・
Refer to [Create Setting board of "Lens alignment chart" and "Viewer"] (Page from A58 to A60) for
how to create.
【
Create Setting board of "Lens alignment chart" and "Viewer"
】
< Lens optical alignment equipment >
CCD camera
Lens alignment equipment
(for center)
LINE GENERATOR
Monitor
- A43・AF-S DX 16-85/3.5-5.6G VR -
MEGALIGHT
100
Lens alignment equipment
(for periphery)
Attachment holder
of the rear lens group
(J19127T)
Page 66
JAA80051-R.3741.A
INC
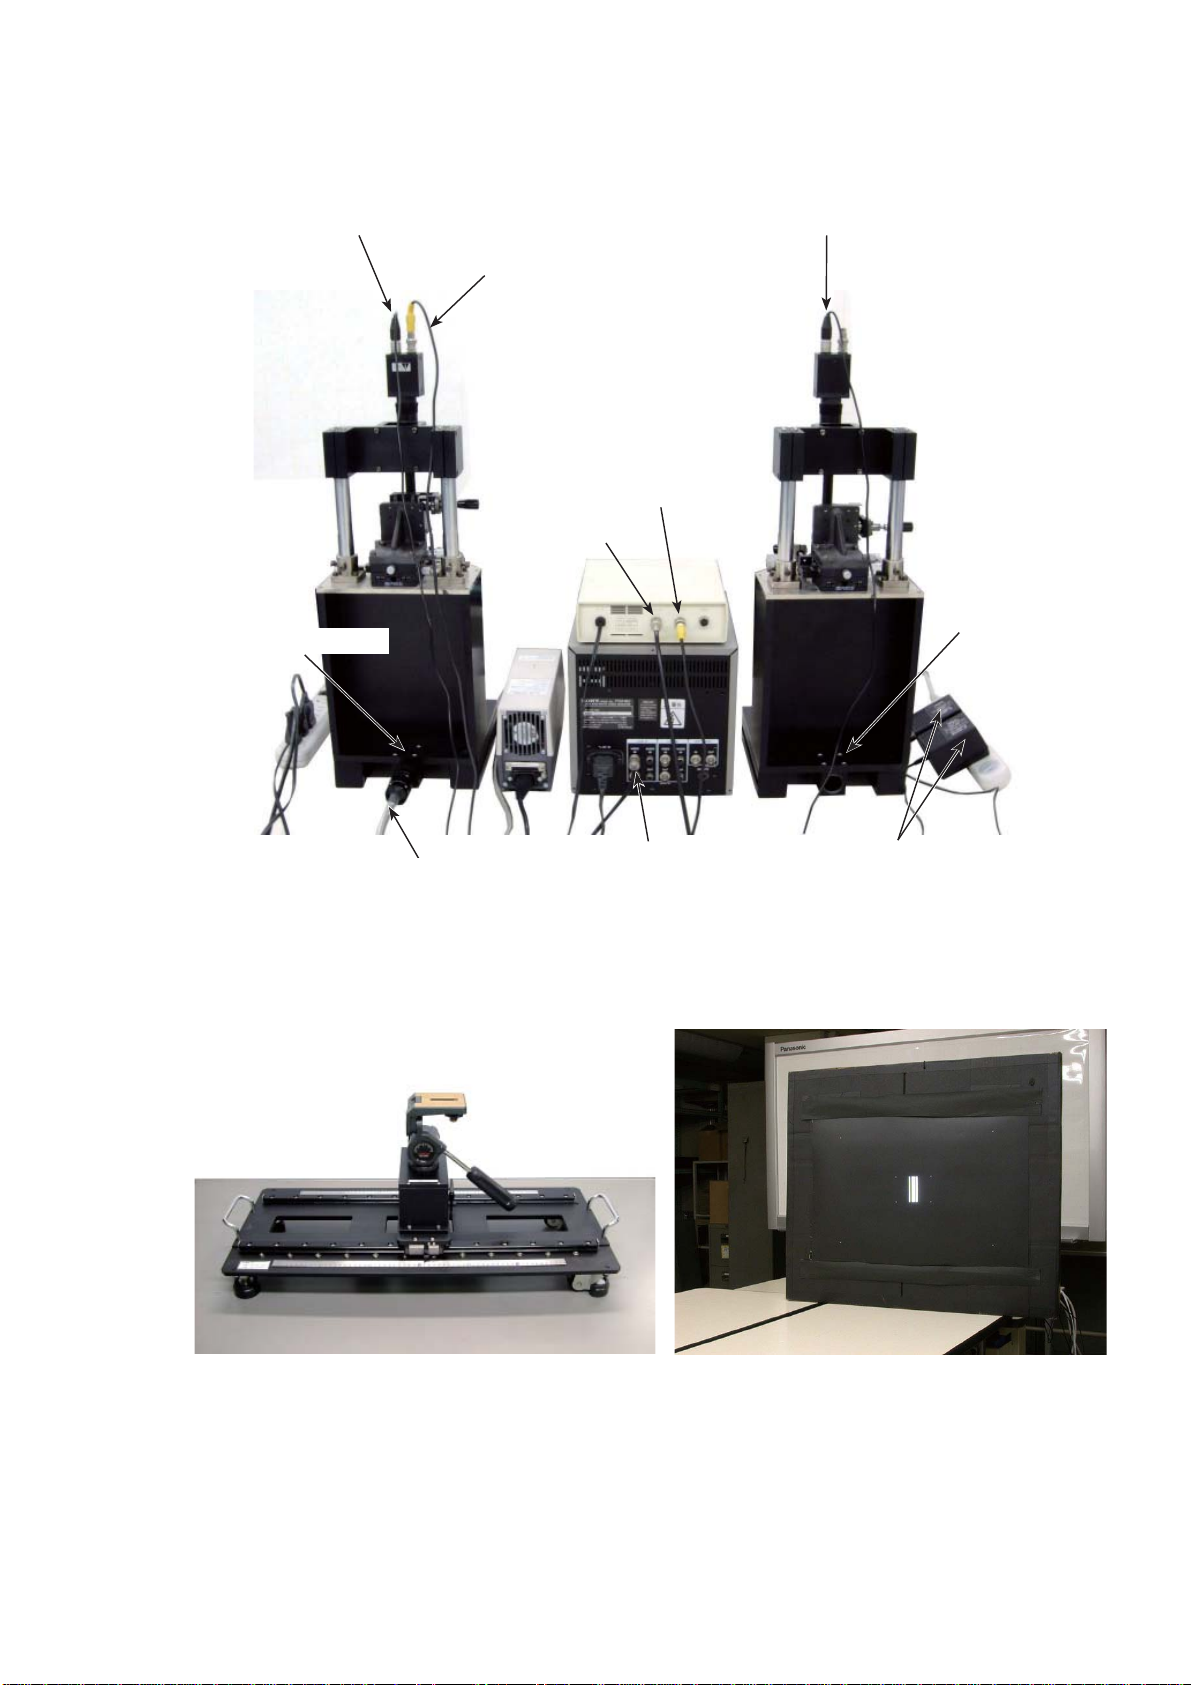
<Back view of Lens optical alignment equipment>
Connect each cable to the appropriate equipment with the same number. (e.g. Connect up ① to ①' )
Power cable for CCD camera
④
'Pinhole chart
③
' Cross line chart
③
Power cable for CCD camera
④
VIDEO cable
①
②
VIDEO OUT
' VIDEO IN
①
' VIDEO IN of 'LINE A
Fiber-optic cable
③
②
< Chart shooting equipment for 4th lens-group alignment >
Slide rail for lens alignment equipment
' Power cable for
④
CCD camera
The chart is embeddied in cardboards.
- A44・AF-S DX 16-85/3.5-5.6G VR -
Page 67
JAA80051-R.3741.A
INC
(2) Center positioning of rear lens-group holder
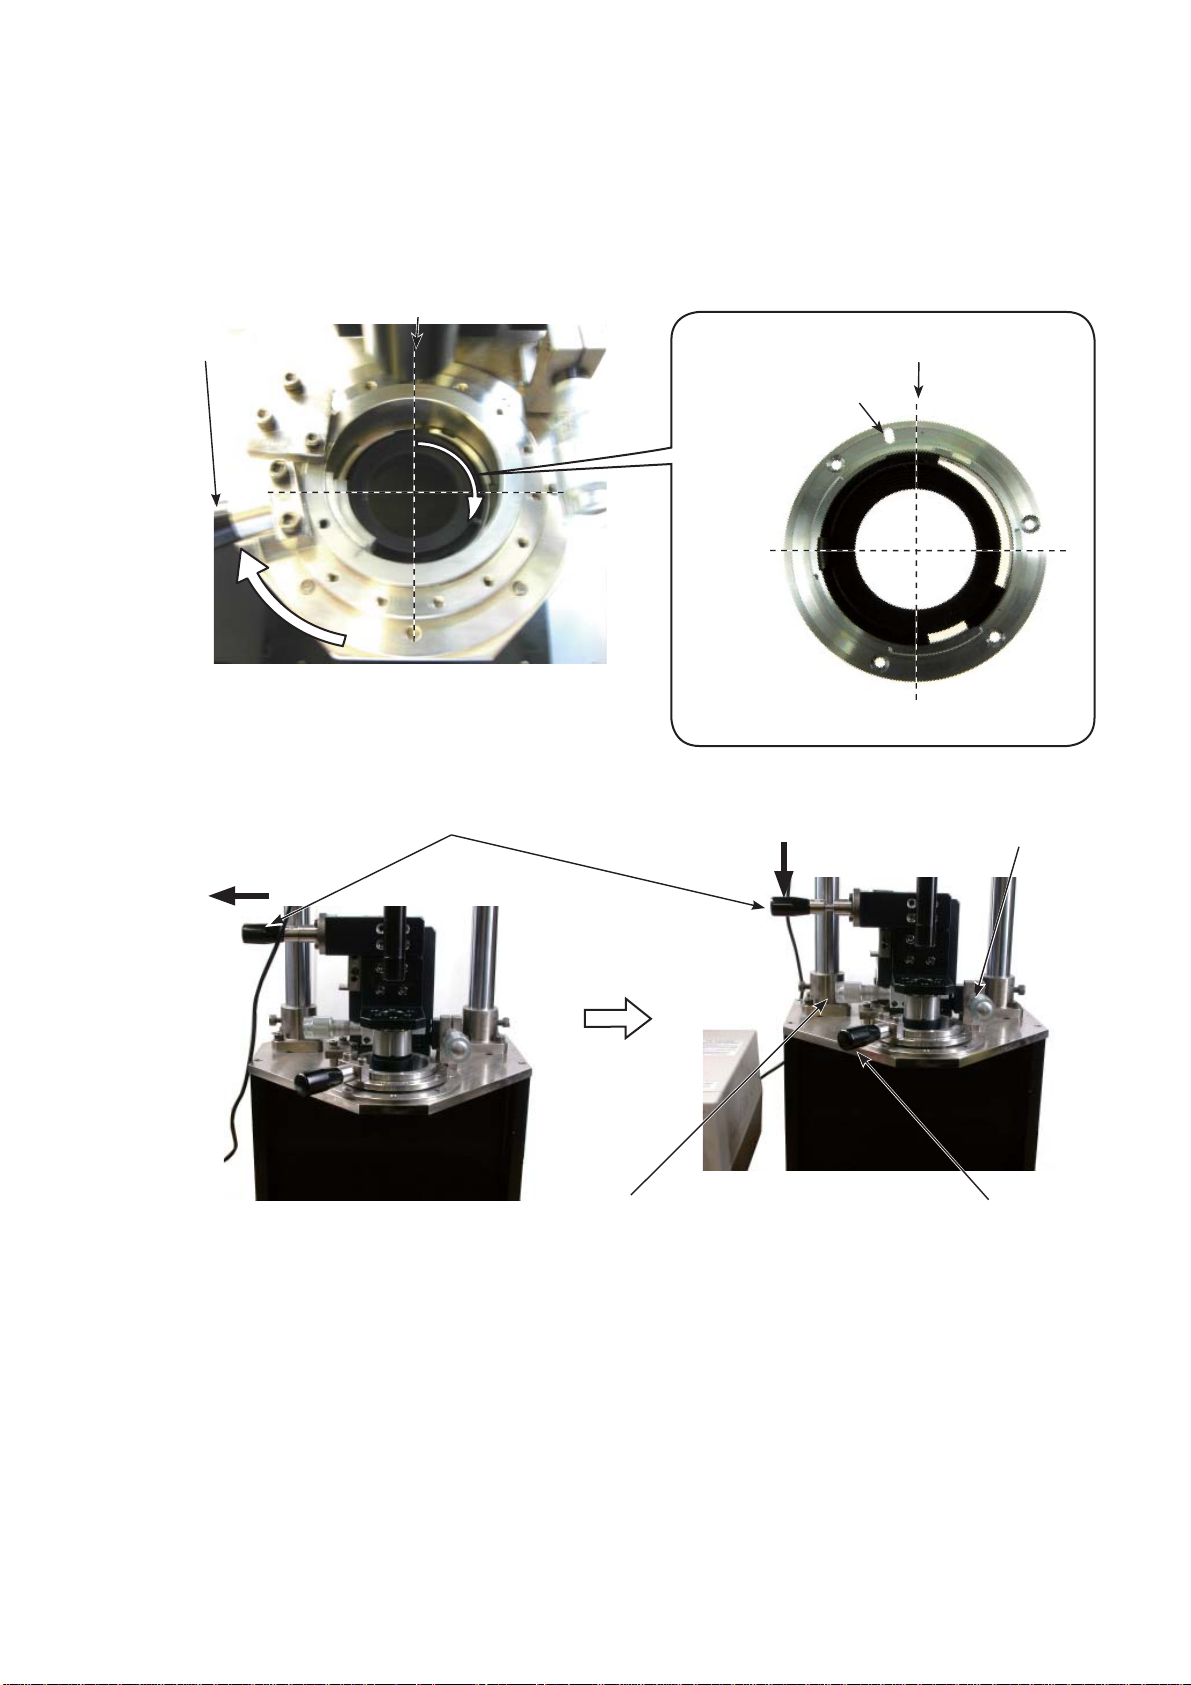
Mount the (self-made) center positioning tool on the lens alignment equipment (for center) by setting the
・
groove in place slightly to the left (in a counterclockwise direction) from the below 12 o’clock position.
Then turn the tool clockwise all the way to the right, and move the lever to the left to fi x it.
12 o'clock position
Fixing lever
Groove for release pin
Lens alignment
equipment
Unlock the holder-moving lever, and move the holder down slowly by the lever.
・
Holder-moving lever
Unlock.
Move down slowly.
Center positioning tool
12 o'clock position
Micrometer for Y-axis
Micrometer for X-axis
・
Adjust the attachment holder (J19127T) position by rotating the micrometers for X-axis or Y-axis so that the
Fixing lever
center of the attachment holder coincides with that of the rear cover ring of the (self-made) center positioning tool.
Caution: Without this alignment, the 4th lens may be damaged by the attachment holder.
・
Move the holder-moving lever of the alignment equipment upwards, and remove the (self-made) center
positioning tool from the equipment by moving the fi xing lever rightwards.
- A45・AF-S DX 16-85/3.5-5.6G VR -
Page 68
JAA80051-R.3741.A
INC
(3) Temporary positioning of the 4th lens group
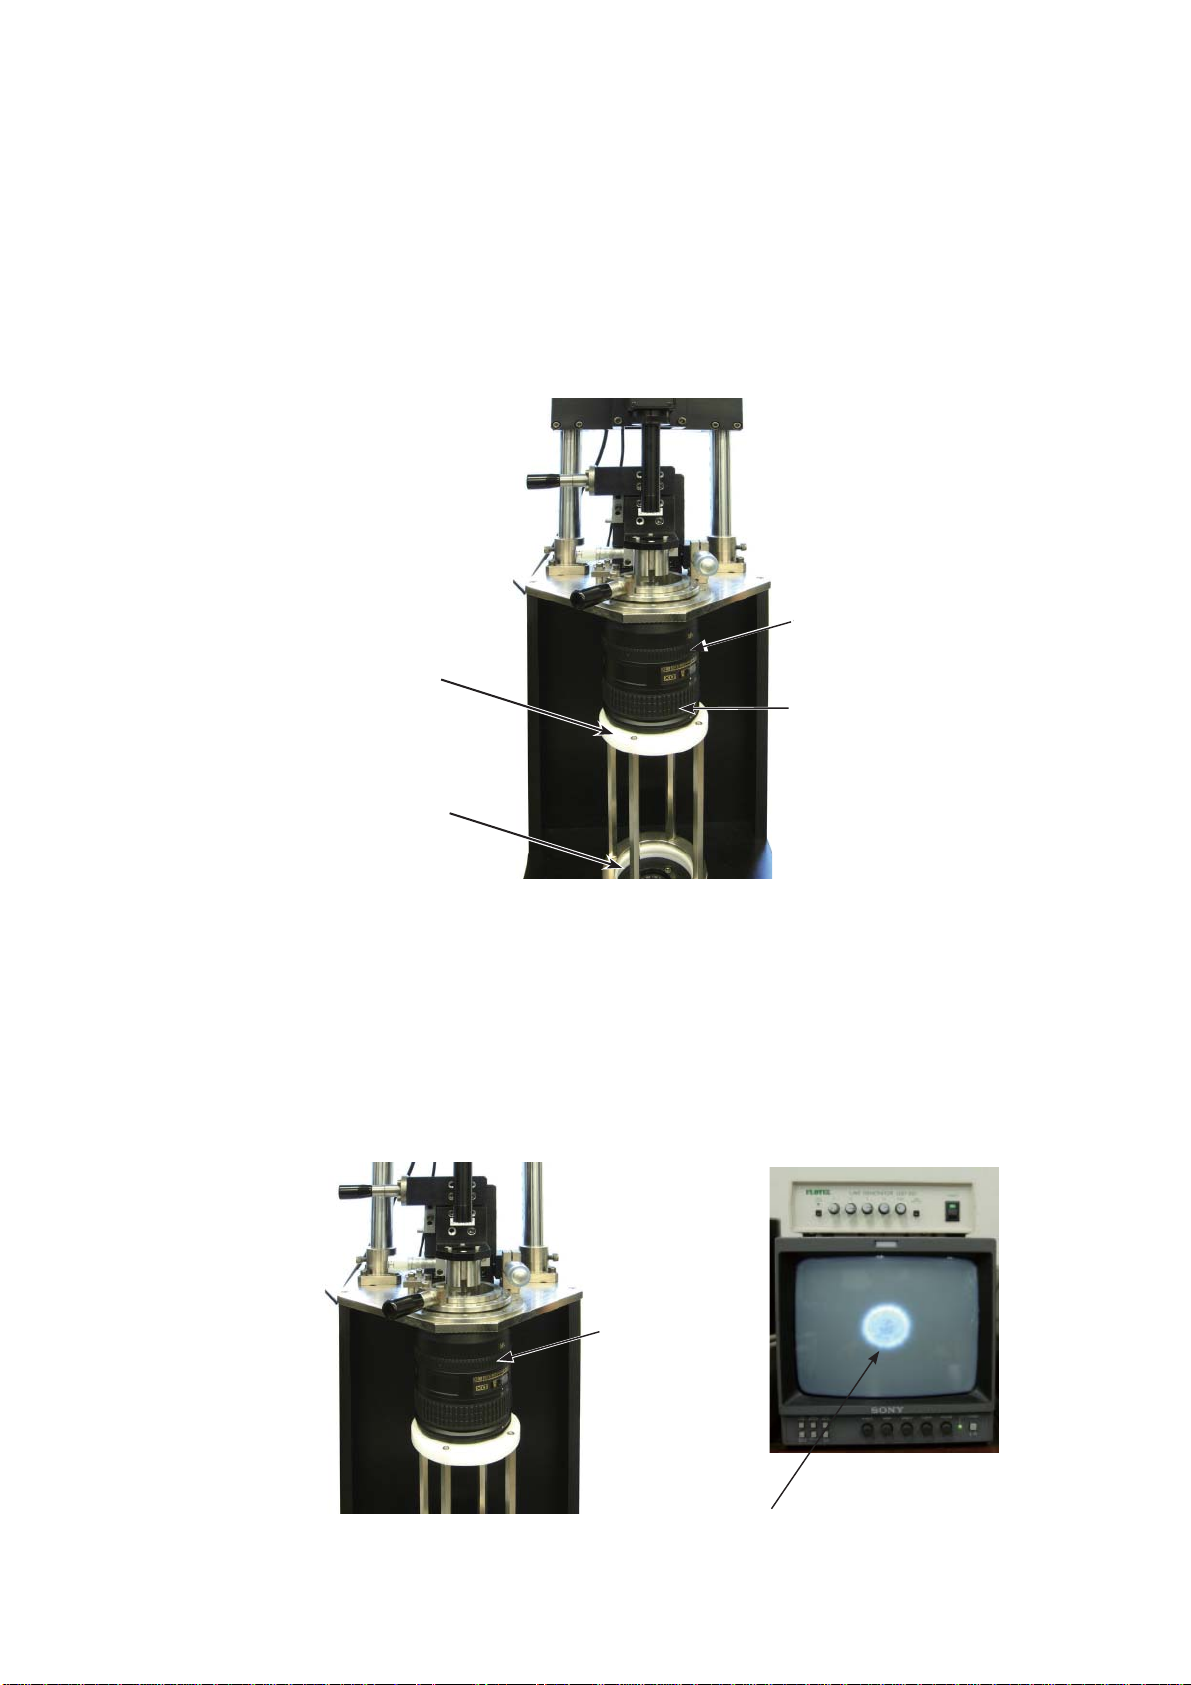
Mount the lens on the lens alignment equipment (for center). Set the focus ring to "infi nity-end".
・
Refer to [(2) Center positioning of rear lens-group holder] (Page A45) for how to mount the lens.
Set the Zoom ring to "16 mm".
・
Place the zoom-fi xing base with the spacer"C", then turn the zoom ring towards TELE until the lens touches
・
the zoom fi xing base.
Focus ring
Zoom-fi xing base
Zoom ring
Spacer"C"
・
Turn each power of the monitor, LINE GENERATOR, and MEGALIGHT 100 to ON.
・
Rotate the "LIGHT CONT."knob of "MEGALIGHT 100" and adjust brightness.
Rotate the focus ring. Adjust the shape of point image so that the point image on the monitor is like bellow.
・
Focus ring
Point image
- A46・AF-S DX 16-85/3.5-5.6G VR -
Page 69
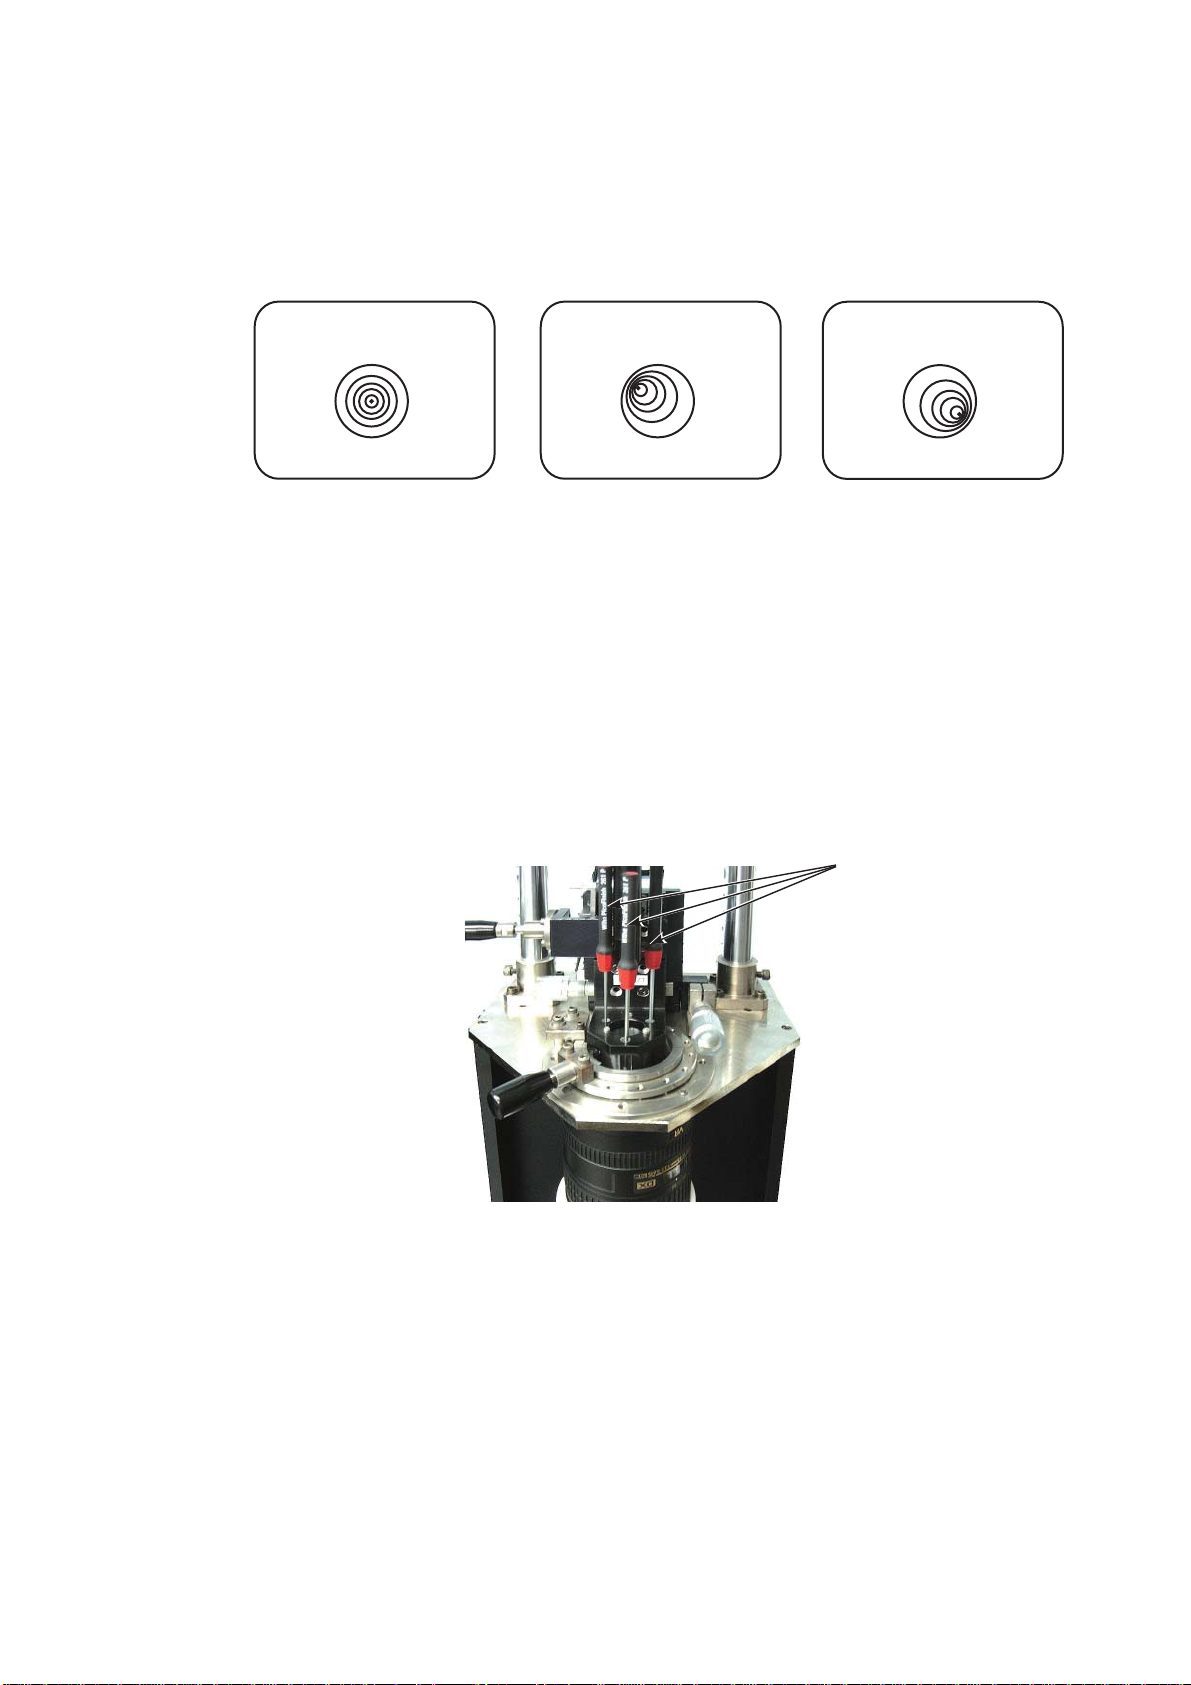
JAA80051-R.3741.A
INC
Check the point image on the monitor.
・
In case the shape is like "Fig.1", remove the lens from the alignment equipment.
In case the point image is like "Fig.2" or "Fig.3", go to the next procedure, and perform "adjustment of 4th
lens group point image".
< 4th lens group point image >
OK
Fig.1 Fig.2
Unlock the holder-moving lever, and move the holder down slowly by the lever.
・
Caution: Be careful NOT to damage the 4th lens group by the attachment holder (J19127T).
Insert the three alignment screwdrivers in the screw holes of the 4th lens unit, and loosen the screws.
・
Caution: When inserting the alignment screwdrivers, move the holder-moving lever up to lock the
holder. Then put them straight down in the screw holes so that the screws can be easily
found. After inserting the alignment screwdrivers, unlock the holder-moving lever and
move the holder down slowly by the lever.
NG
Alignment screwdrivers
NG
Fig.3
Rotate the micrometer (X-axis and Y-axis) so that the point image on the monitor is like "Fig.1".
・
When the point image becomes like the above "Fig.1", tighten the three (loosened) screws of the 4th lens-G
・
unit with the below three alignment screwdrivers.
Remove the three alignment screwdrivers from the attachment holder (J19127T).
・
Move the holder-moving lever up slowly to lock the holder, and remove the lens from the equipment (for
・
center).
- A47・AF-S DX 16-85/3.5-5.6G VR -
Page 70
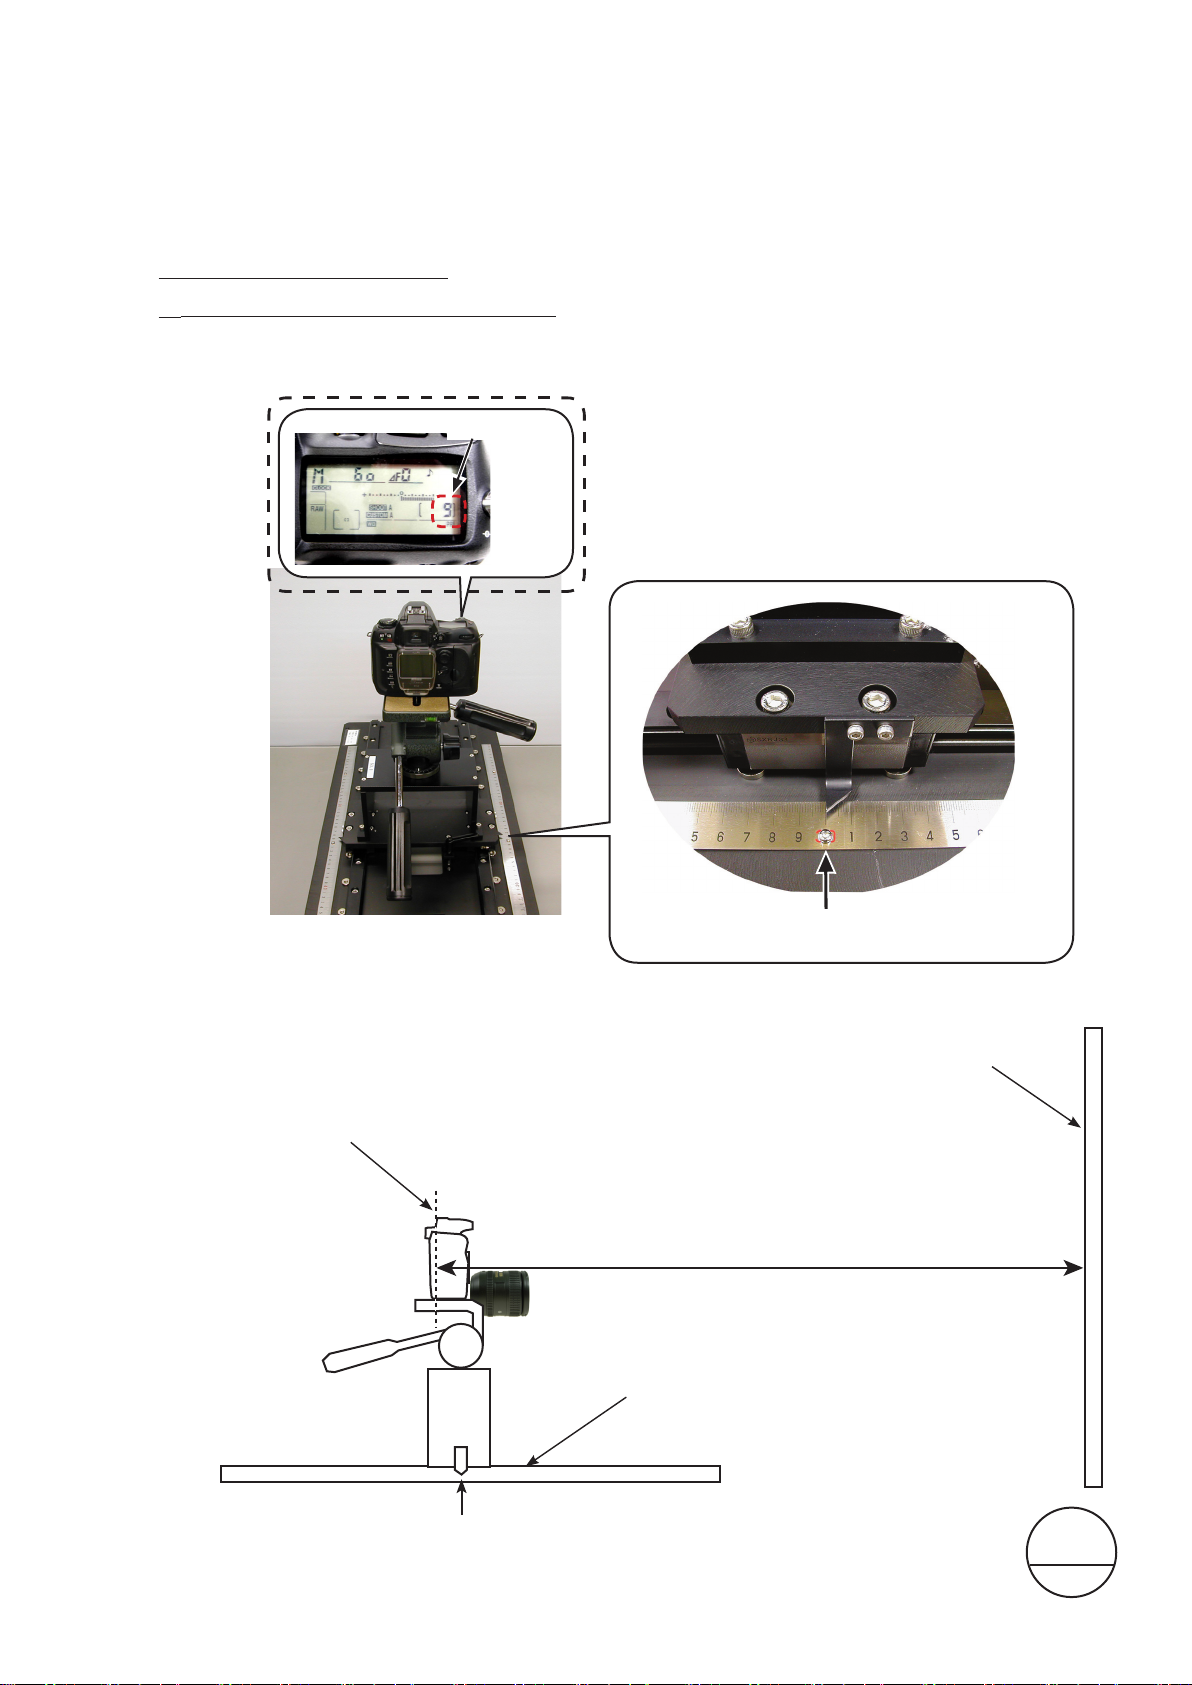
JAA80051-R.3741.A
INC
(4) Chart shooting for the rear lens group alignment
Prepare a camera (D200). Set the shutter speed to "M1/60", aperture to "full open", and the focus mode to
"S". On the shooting menu, set "Image Quality" mode to "RAW", "WB" to "Preset" and "ISO" to "200".
Set the VR mode of the lens to "OFF".
Insert CF card into the camera
△(Deletion)
Check that the counter shows “2” or more.
Set up the camera (D200) on a tripod on the slide rail. Set the indication pointer of the tripod to 30 cm.
△(Deletion)
counter
△(Deletion)
Set the alignment chart (J19128) as shown below.
Focal plane mark of camera
Rail tool
Back
30 cm
Alignment chart
(J19128)
Magnications: 40
(Zoom position: 16 mm)
75 cm±2 cm
Front
Changed page
△× 3
30 cm
Page 71
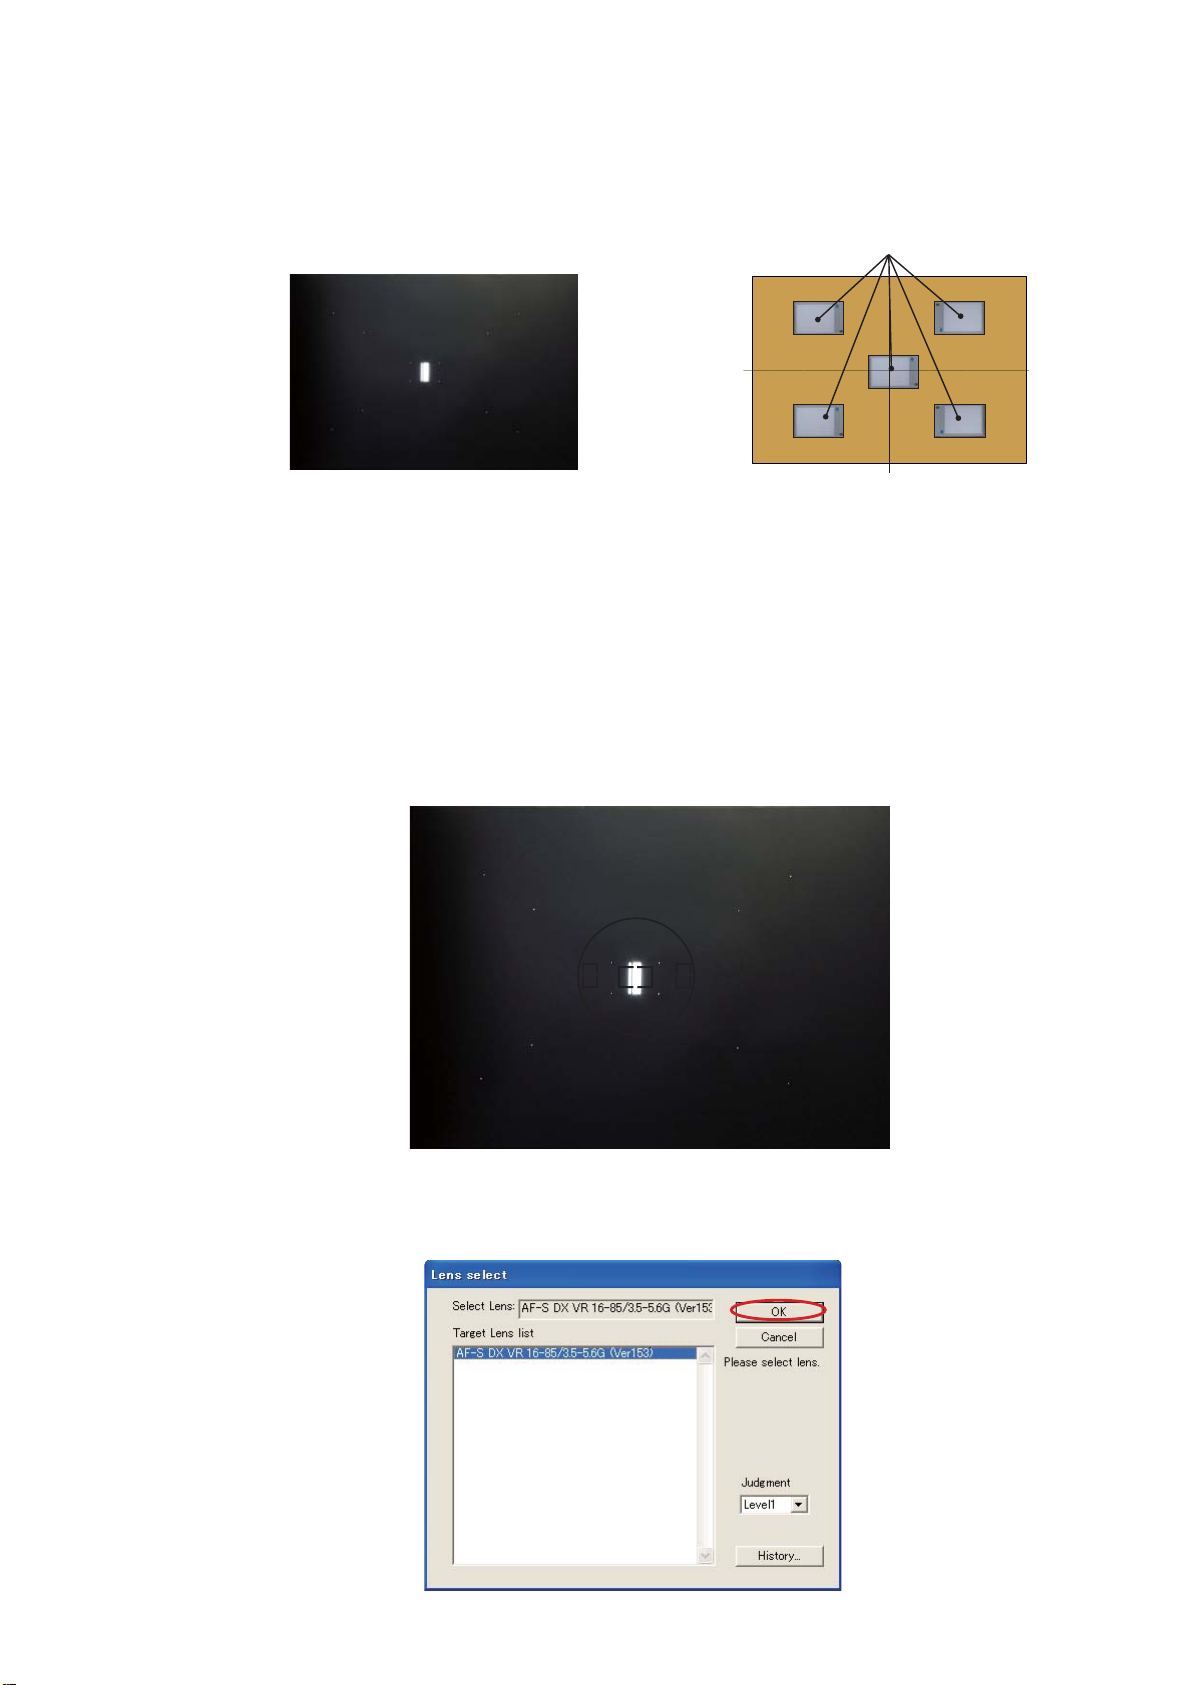
JAA80051-R.3741.A
INC
・
Turn the power of viewers (5 pcs.) to ON.
Caution: If the batteries of viewers are exhausted causing decreased brightness, the shooting data
cannot be obtained correctly.
Viewer× 5 pcs.
Front
Attach the suspected lens to the camera (D200). Set the A/M change SW to "M", the zoom ring to "24 mm",
・
and the focus ring to "infi nity".
Set the A/M change SW to "M/A".
・
By looking through the viewfi nder, adjust the height and tilt to make the chart fi ll the entire fi nder fi eld
・
frame.
Adjust the tilt of the slide rail to make the three chart lines position in the center of the viewfi nder, when the
・
tripod is slid all the way to the front and back.
Back
Connect the PC and camera via USB cable (Camera setting for USB: PTP).
・
Start the adjustment software (LWM_AFSDXVR16_85.exe).
・
Click "OK".
・
- A49・AF-S DX 16-85/3.5-5.6G VR -
Page 72
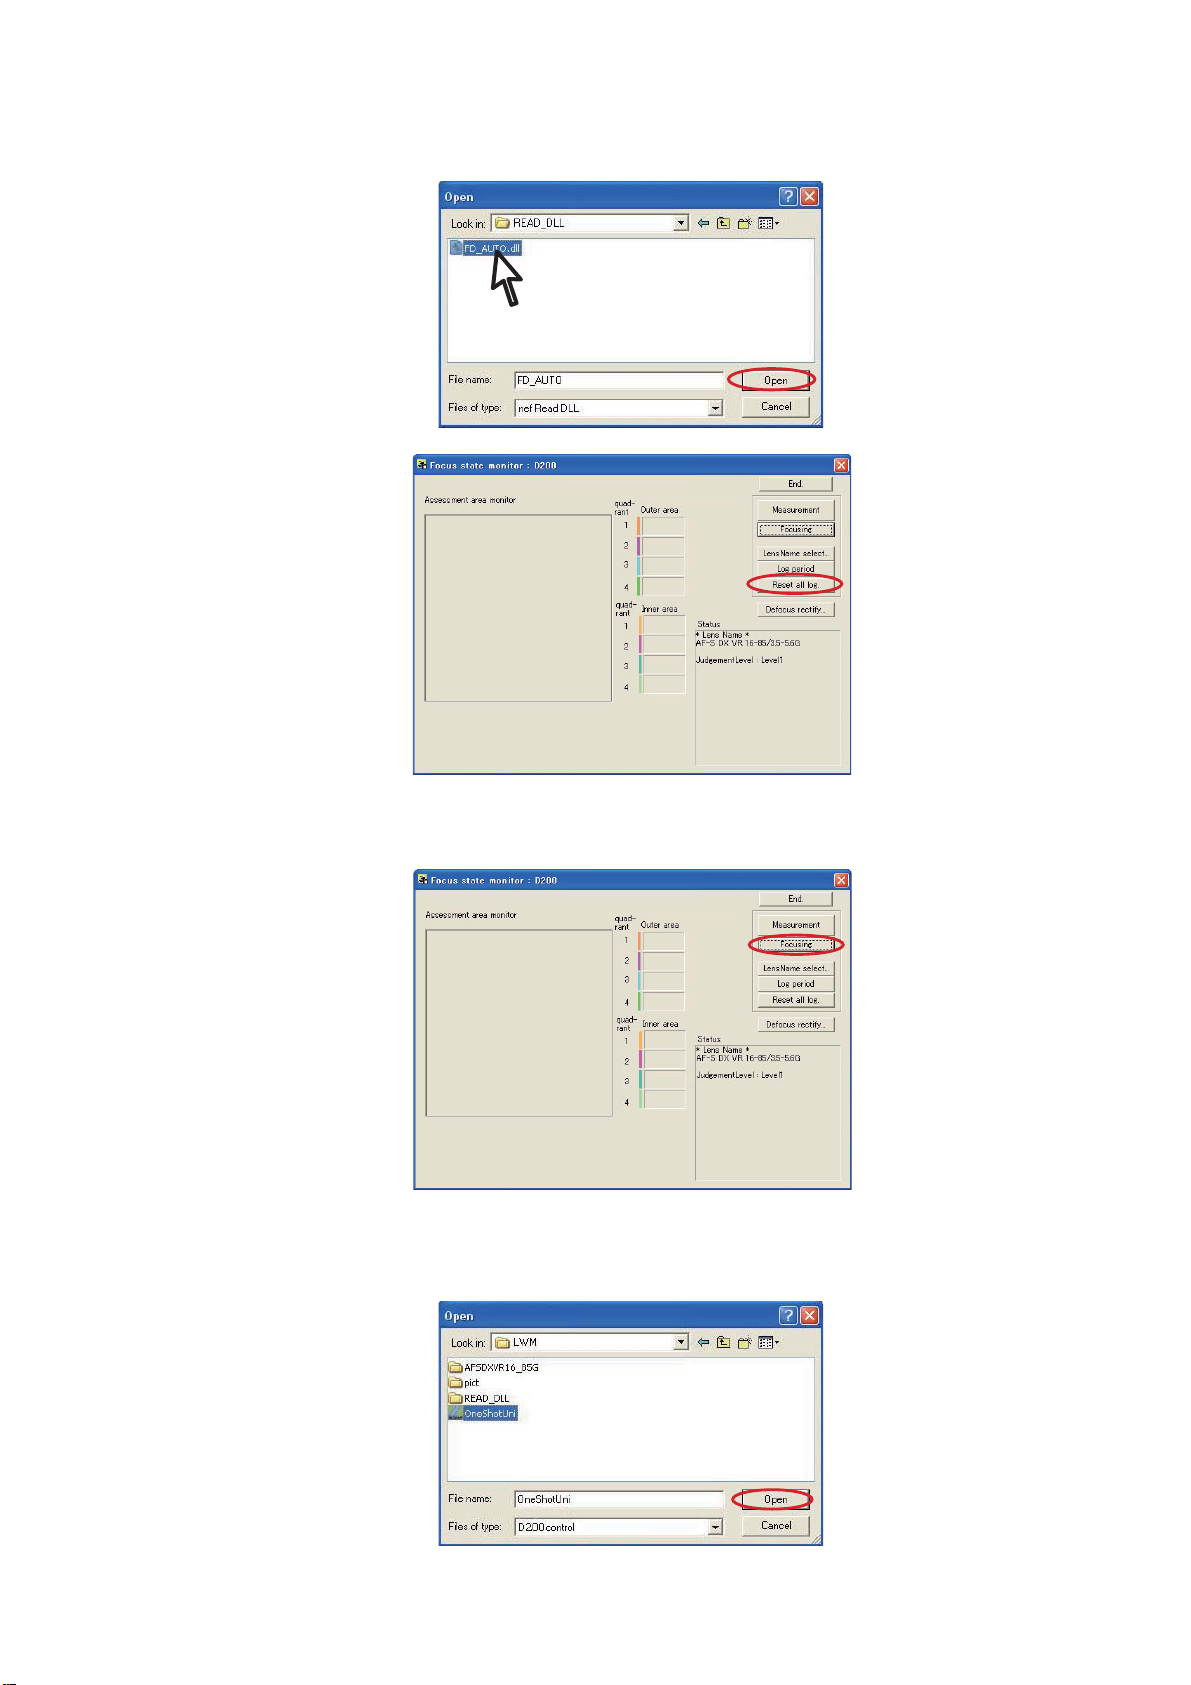
JAA80051-R.3741.A
INC
If this software is used for the fi rst time, the selection screen of reading data will appear. This does not
※
appear after the 2nd-time usage. Select "FD_AUTO.dll" and click "Open".
Click "Reset all Log".
・
・After darken the room, click "Focusing". AF is activated to focus and the shutter is released.
If this software is used for the fi rst time, the software selection screen will appear. This does not appear
※
after the 2nd-time usage.Select "OneShotUni" and click "Open".
- A50・AF-S DX 16-85/3.5-5.6G VR -
Page 73
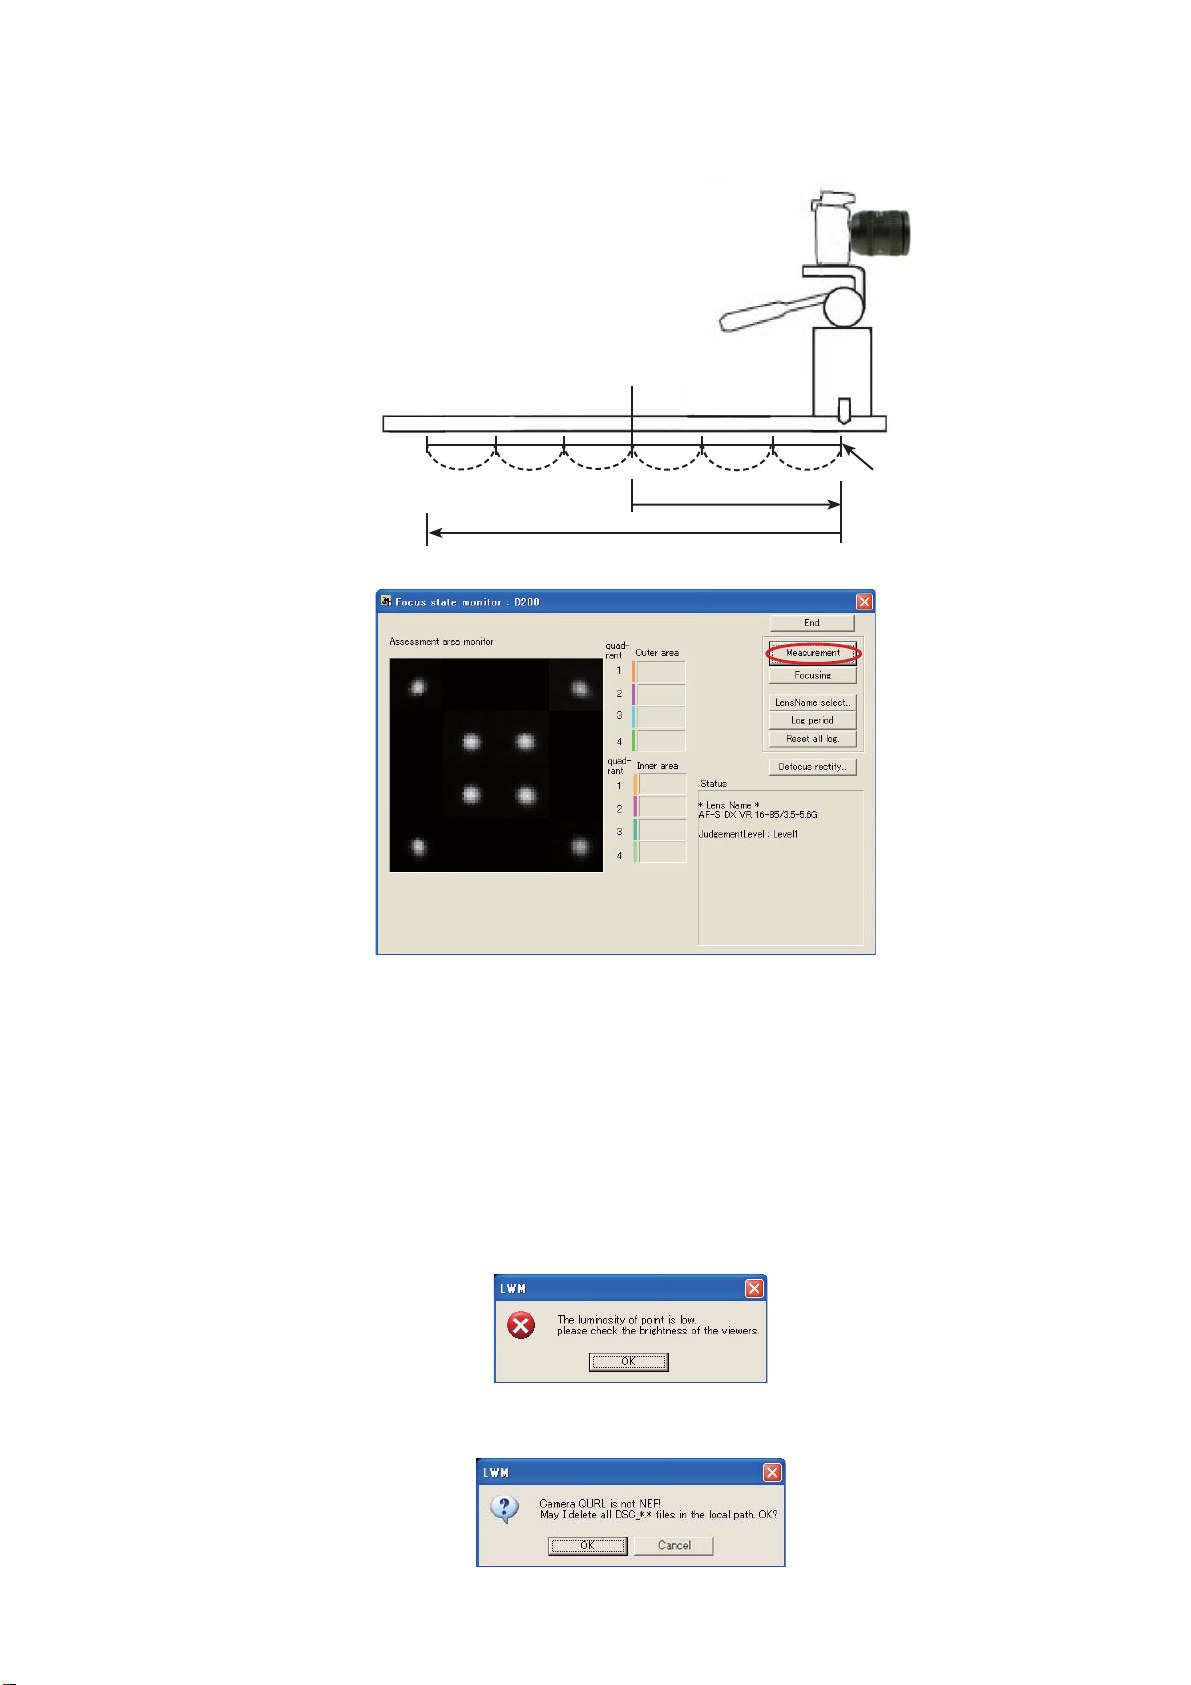
Set the A/M change SW to "M".
INC
・
Slide the tripod to the front by 18±0.1 cm. Click "Measurement".
・
Focusing Position
To Back
JAA80051-R.3741.A
To Front
6cm
When the shutter of the camera is released, slide the tripod to the back by 6±0.1 cm and click "Measurement"
・
again.
6cm
6cm
36cm
6cm 6cm 6cm
18cm
Measuring Position
Repeat this procedure (of sliding the tripod in increments of 6±0.1 cm and clicking "Measurement"
・
at 7 measuring positions). The total sliding distance is 36 cm. (ref. Illustration of previous page)
Note 1: When the below warning is given, there may be some defects in the brightness of the viewers
and/or parallelism of the chart and camera, etc. So correct the above and make a remeasurement.
Note 2: When the below warning is given, recheck that the Quality mode of the camera is set to RAW.
- A51・AF-S DX 16-85/3.5-5.6G VR -
Page 74
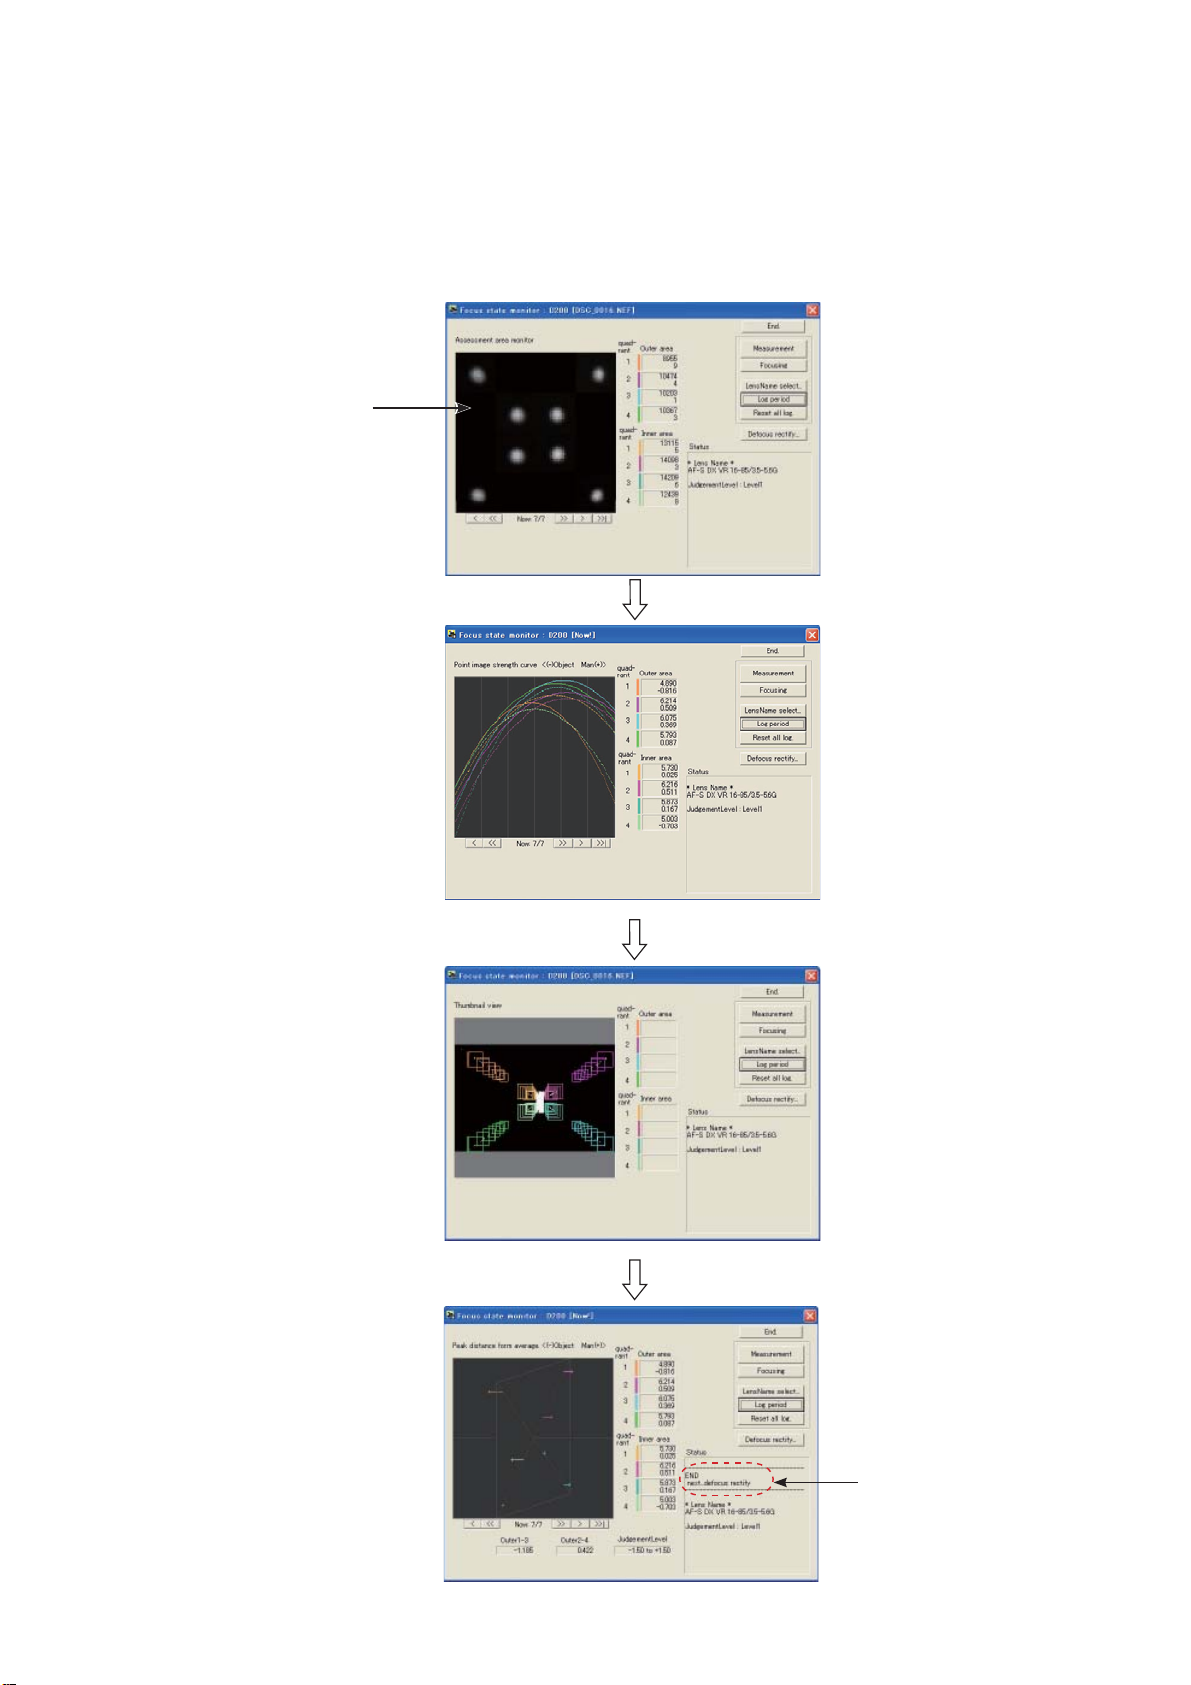
JAA80051-R.3741.A
INC
After the seven measurements, point the cursor to the confi rmation screen of the software. Click it three
・
times.
If "Information" displays "END", the lens optical alignment is completed.
If "Information" displays other than "END", go to the next "(5) 4th lens group alignment" (Page A53) to
readjust.
Confi rmation screen
Information display
- A52・AF-S DX 16-85/3.5-5.6G VR -
Page 75
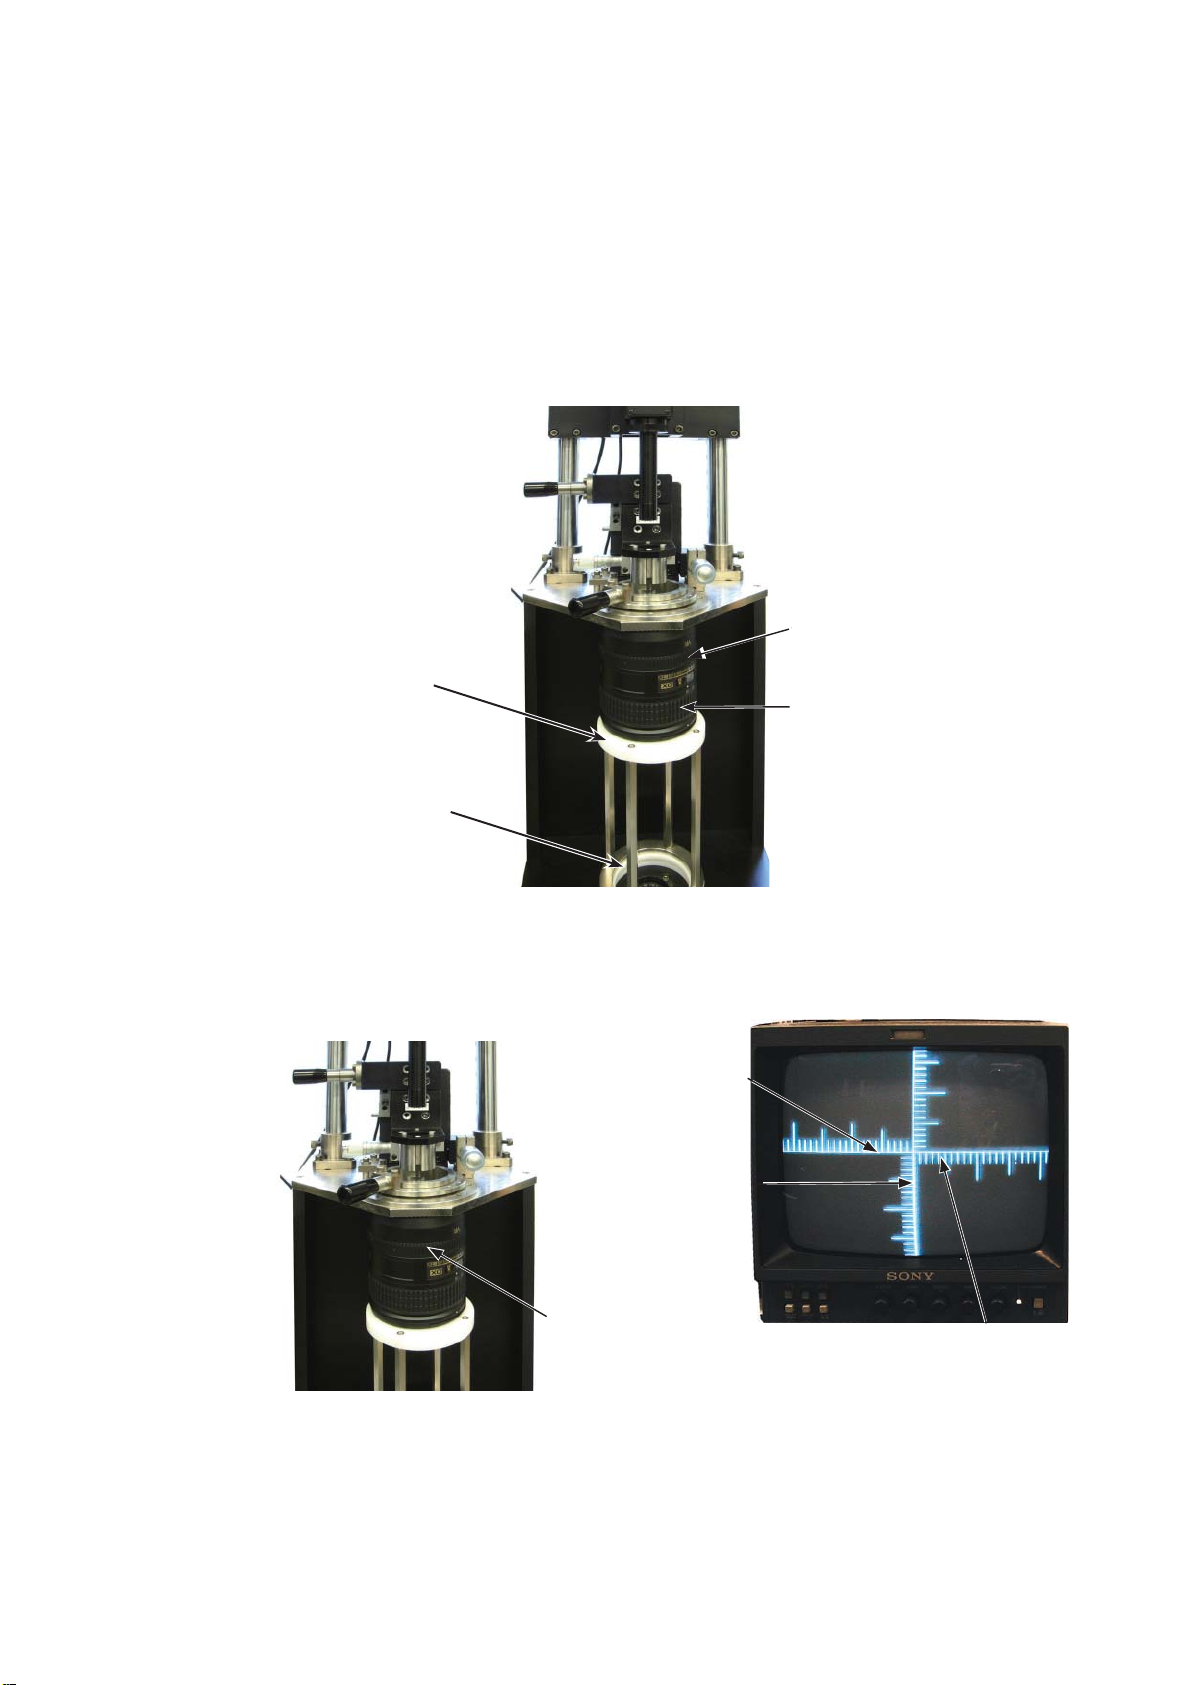
JAA80051-R.3741.A
INC
(5) 4th lens group alignment
・Mount the lens on the equipment (for periphery).
Refer to [(2) Center positioning of rear lens-group holder] (Page A45) for how to mount the lens.
Set the zoom ring to "16 mm"
・
Place the zoom-fi xing base with the spacer"C", then turn the zoom ring towards TELE until the lens touches
・
the zoom fi xing base..
Focus ring
Zoom-fi xing base
Zoom ring
Spacer"C"
・
Turn each power of the monitor, LINE GENERATOR, and MEGALIGHT 100 to ON.
Adjust the calibrated cross lines by rotating the "LIGHT CONT." knob of "MEGALIGHT 100" and rotating
the focus ring from "infi nity"-end so that the intersection of the cross lines can be seen clearly.
Y-axis
X-axis
Focus ring
Caution:
In case the cross lines are tilted, adjust them by
turning the chart, which is screwed in the rear
tube of the equipment.
Unlock the holder-moving lever, and move the holder down slowly by the lever.
・
Caution: Be careful NOT to damage the 4th lens group by the attachment holder (J19127P).
- A53・AF-S DX 16-85/3.5-5.6G VR -
Cross lines
Page 76
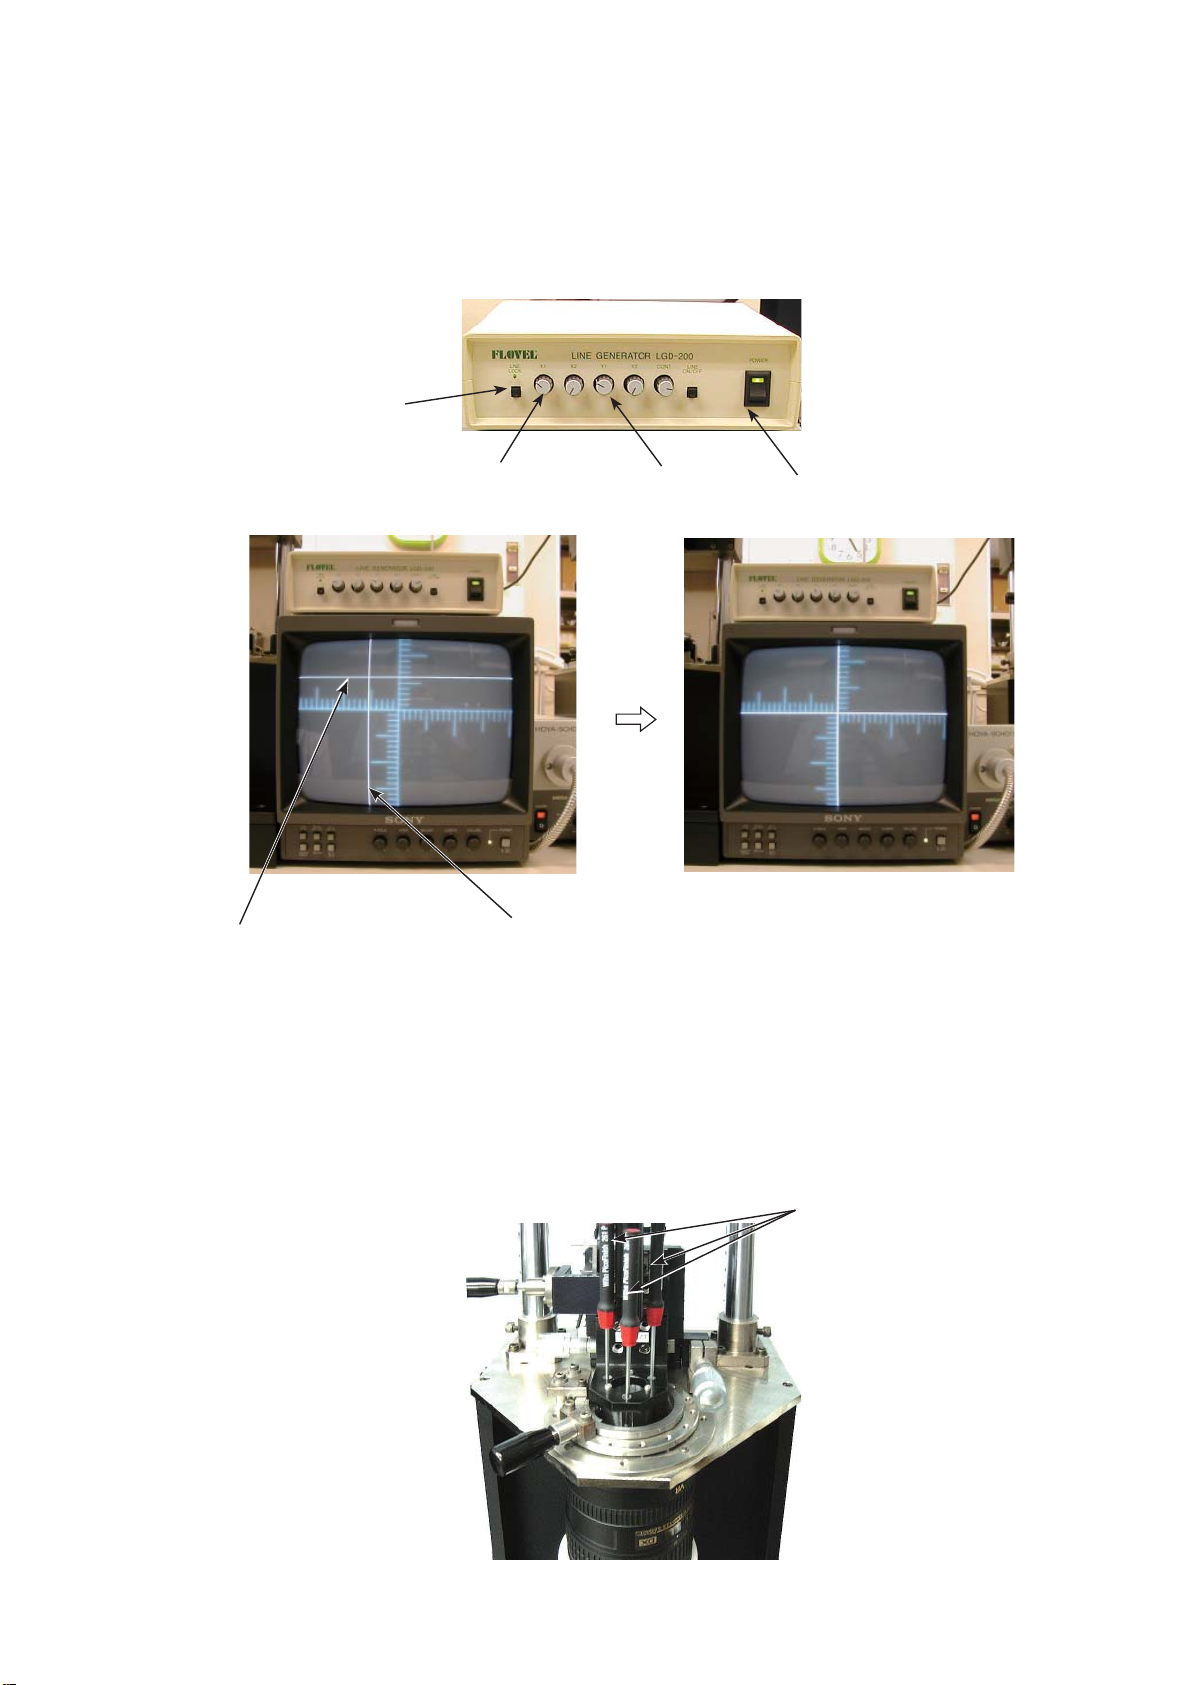
JAA80051-R.3741.A
INC
Press the "LINE ON/OFF" button of LINE GENERATOR. Turn the knobs of "X1" and "Y1" until X- and
・
Y-lines are displayed on the monitor.
Move these X- and Y-lines so that they coincide with the cross lines of the CCD camera.
Then press "LINE LOCK" button to fi x these X- and Y-lines.
"LINE LOCK" button
X1 knob
LINE GENERATOR
X-line
Insert the three alignment screwdrivers in the screw holes of the 4th lens unit, and loosen the screws.
・
Caution: When inserting the alignment screwdrivers, move the holder-moving lever up to lock the
Y-line
Y1 knob
"LINE ON/OFF" button
holder. Then put them straight down in the screw holes so that the screws can be easily
found. After inserting the three alignment screwdrivers, unlock the holder-moving lever,
and move the holder down slowly by the lever.
Alignment screwdrivers
- A54・AF-S DX 16-85/3.5-5.6G VR -
Page 77
JAA80051-R.3741.A
INC
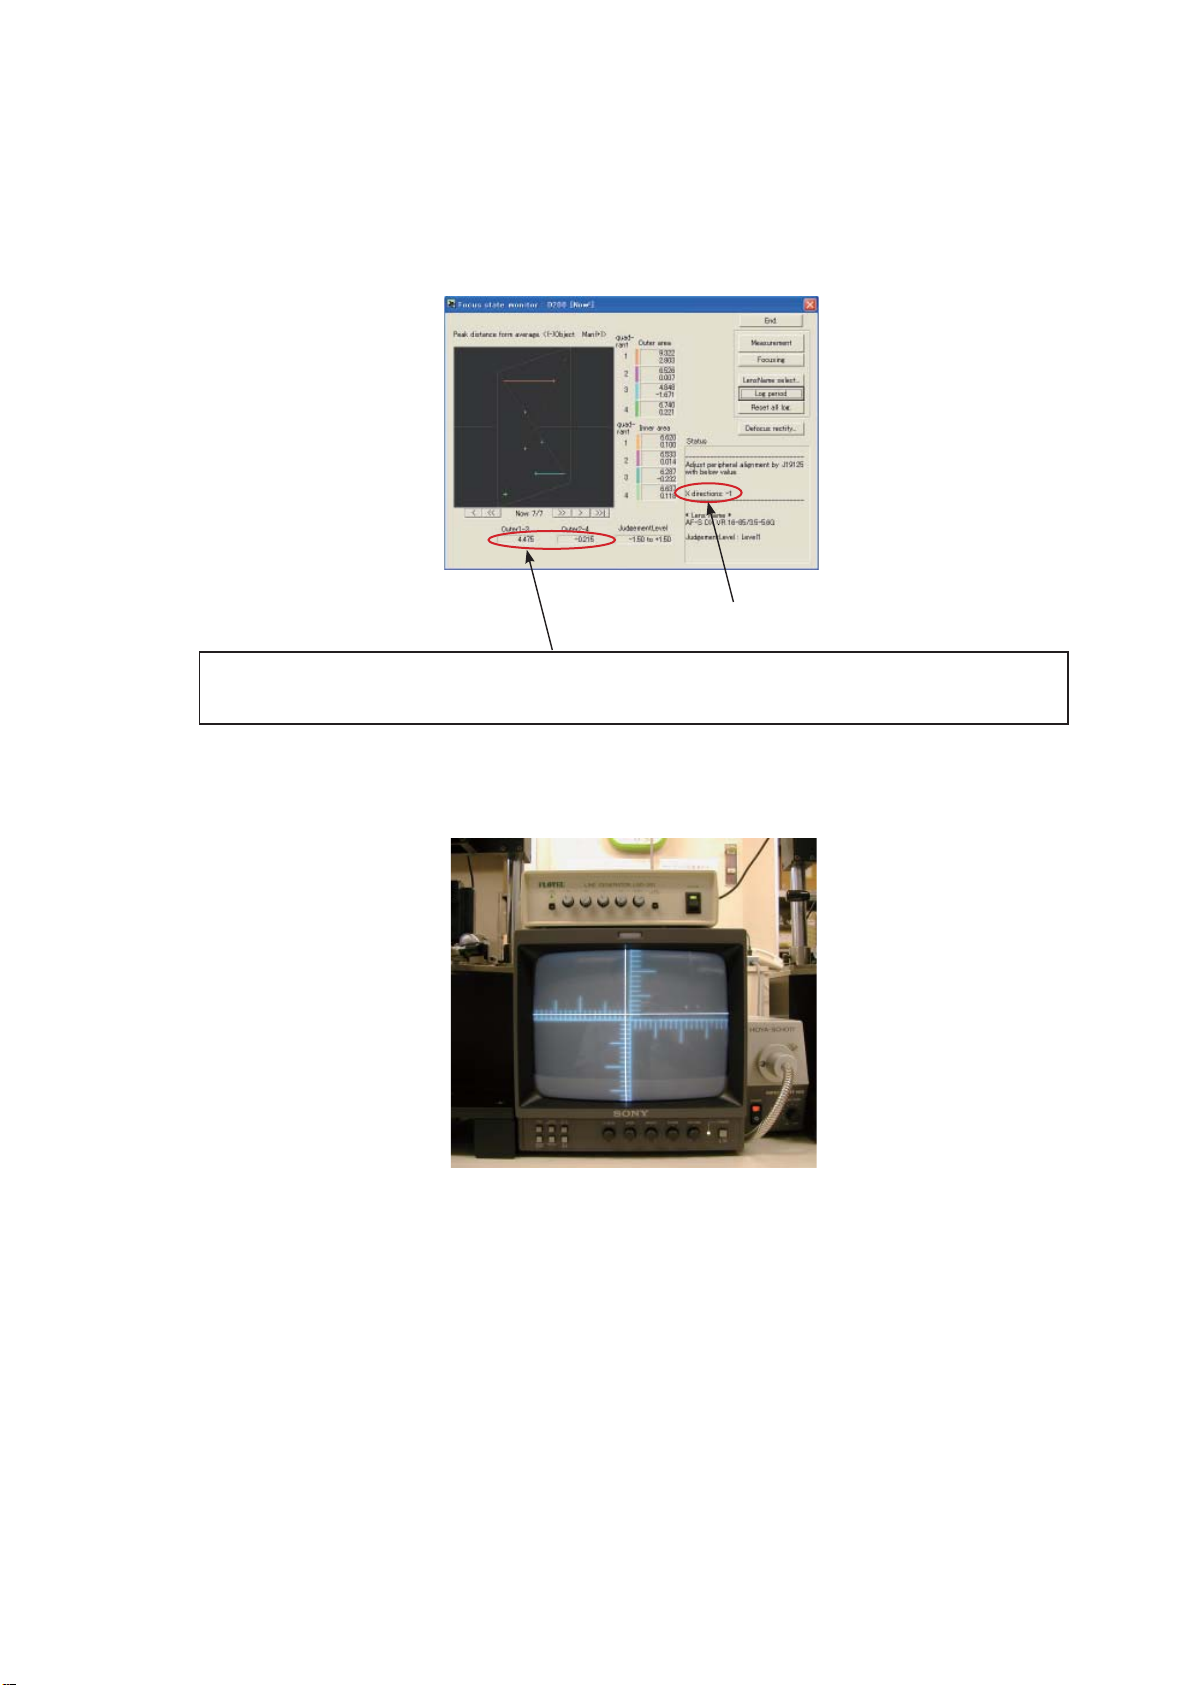
・Rotate the knobs of the micrometer (X and Y axes), and shift the calibrated cross lines based on the result
(values) of the chart shooting of the rear lens group alignment.
Caution: When the knobs of the micrometer (X and Y axes) are rotated but the calibrated cross lines
are unable to move, do not forcedly rotate them.
Result (values)
If more accuracy is preferable even if "END" is displayed, adjust by using the value of "Outer 1-3" as the
adjustment amount for "X-axis", while the value of "Outer 2-4" as the adjustment amount for "Y-axis".
< e.g. (X directions:+1, Y directions:-1) >
・After completing the above shift, tighten three screws of the 4th lens unit with the alignment screwdrivers.
Remove the alignment screwdrivers from the attachment holder (J19127T).
・
- A55・AF-S DX 16-85/3.5-5.6G VR -
Page 78
JAA80051-R.3741.A
INC
Move the holder-moving lever up to lock the holder.
・
Check that shift amounts (caused by differences between the calibrated cross lines and the X/Y lines) are
・
equal to the result (values) (1= 1 scale amount of the calibrated cross lines) of "Chart shooting of the rear
lens group alignment".
Caution: After fi xing the three screws of the 4th lens unit, if the shift amounts are different from the
result of the chart shooting, repeat the rear lens group alignment until they become equal.
Turn each power of the monitor, LINE GENERATOR, and MEGALIGHT 100 to OFF.
・
Remove the lens from the equipment (for periphery).
Go back to [(4) Chart shooting for the rear lens group alignment] (Page A48).
・
Repeat this procedure of [(4) Chart shooting for the rear lens group alignment] (Page A48) and
[(5) 4th lens group alignment] (Page A53) until the result become "END".
- A56・AF-S DX 16-85/3.5-5.6G VR -
Page 79
JAA80051-R.3741.A
INC
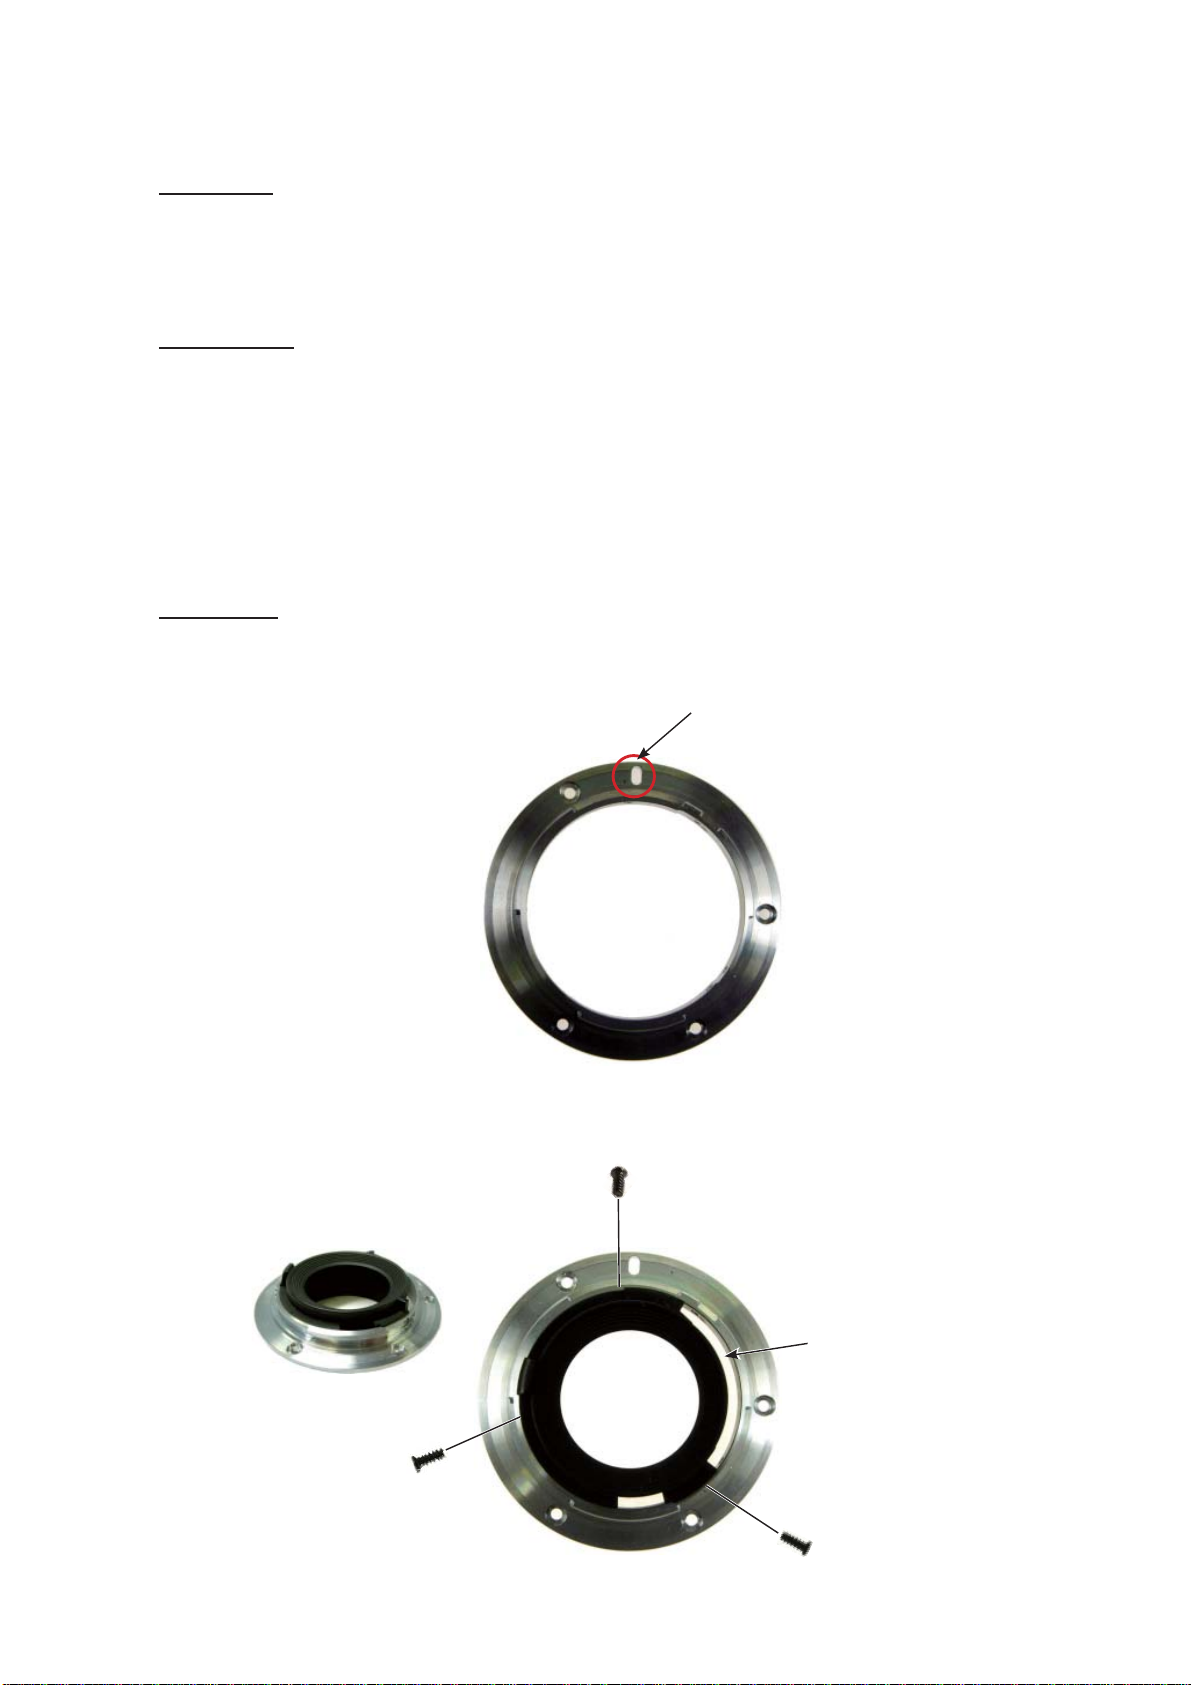
Create positioning tool of Rear lens-group holder for lens alignment
【
1.Summery
This is a positioning tool of the rear lens group holder for lens alignment, in order to secure the position for
attaching the rear lens group temporarily.
2.Preparation
The following devices are used:
*Rear cover ring (#39. :1K631-959) ×1
*Bayonet mount unit (1C999-645) ×1
For use, remove the other components than the bayonet mount section from the bayonet mount unit of RP.
*Screw (#118. :1K010-002-1) ×3
3.Procedure
Put the bayonet mount as below.
・
】
Put with the groove, in which the lock pin of camera body enters, facing upwards.
Mount the rear cover ring on the bayonet mount, and fi x them with three screws.
・
Large cutout of rear cover ring.
- A57・AF-S DX 16-85/3.5-5.6G VR -
Page 80
JAA80051-R.3741.A
How to create Setting board for "Lens alignment chart" and "Viewer"
INC
How to create Setting board for "Lens alignment chart" and "Viewer"
1. Summary
In order to take pictures of the special chart with a digital camera and get necessary data for lens alignment, this
board is created to use for setting a special chart and light viewers (for chart illumination).
2. Preparation
Device
Light viewer (for J19134): J19128A
・
(Size: 154×245mm) 5 pcs.
Lens alignment chart (for D3): J19128
・
Size: 840×1250mm) 1 pc.
Board or cardboard box
・
(Size: 840×1250×20mm) 1 pc.
(Note) Because it is necessary to cut out for fi tting the light viewers, choose cardboard boxes or material which
can be easily cut.
3. Procedure(In this document, 2 cardboard boxes (840×1250×10mm) are used.)
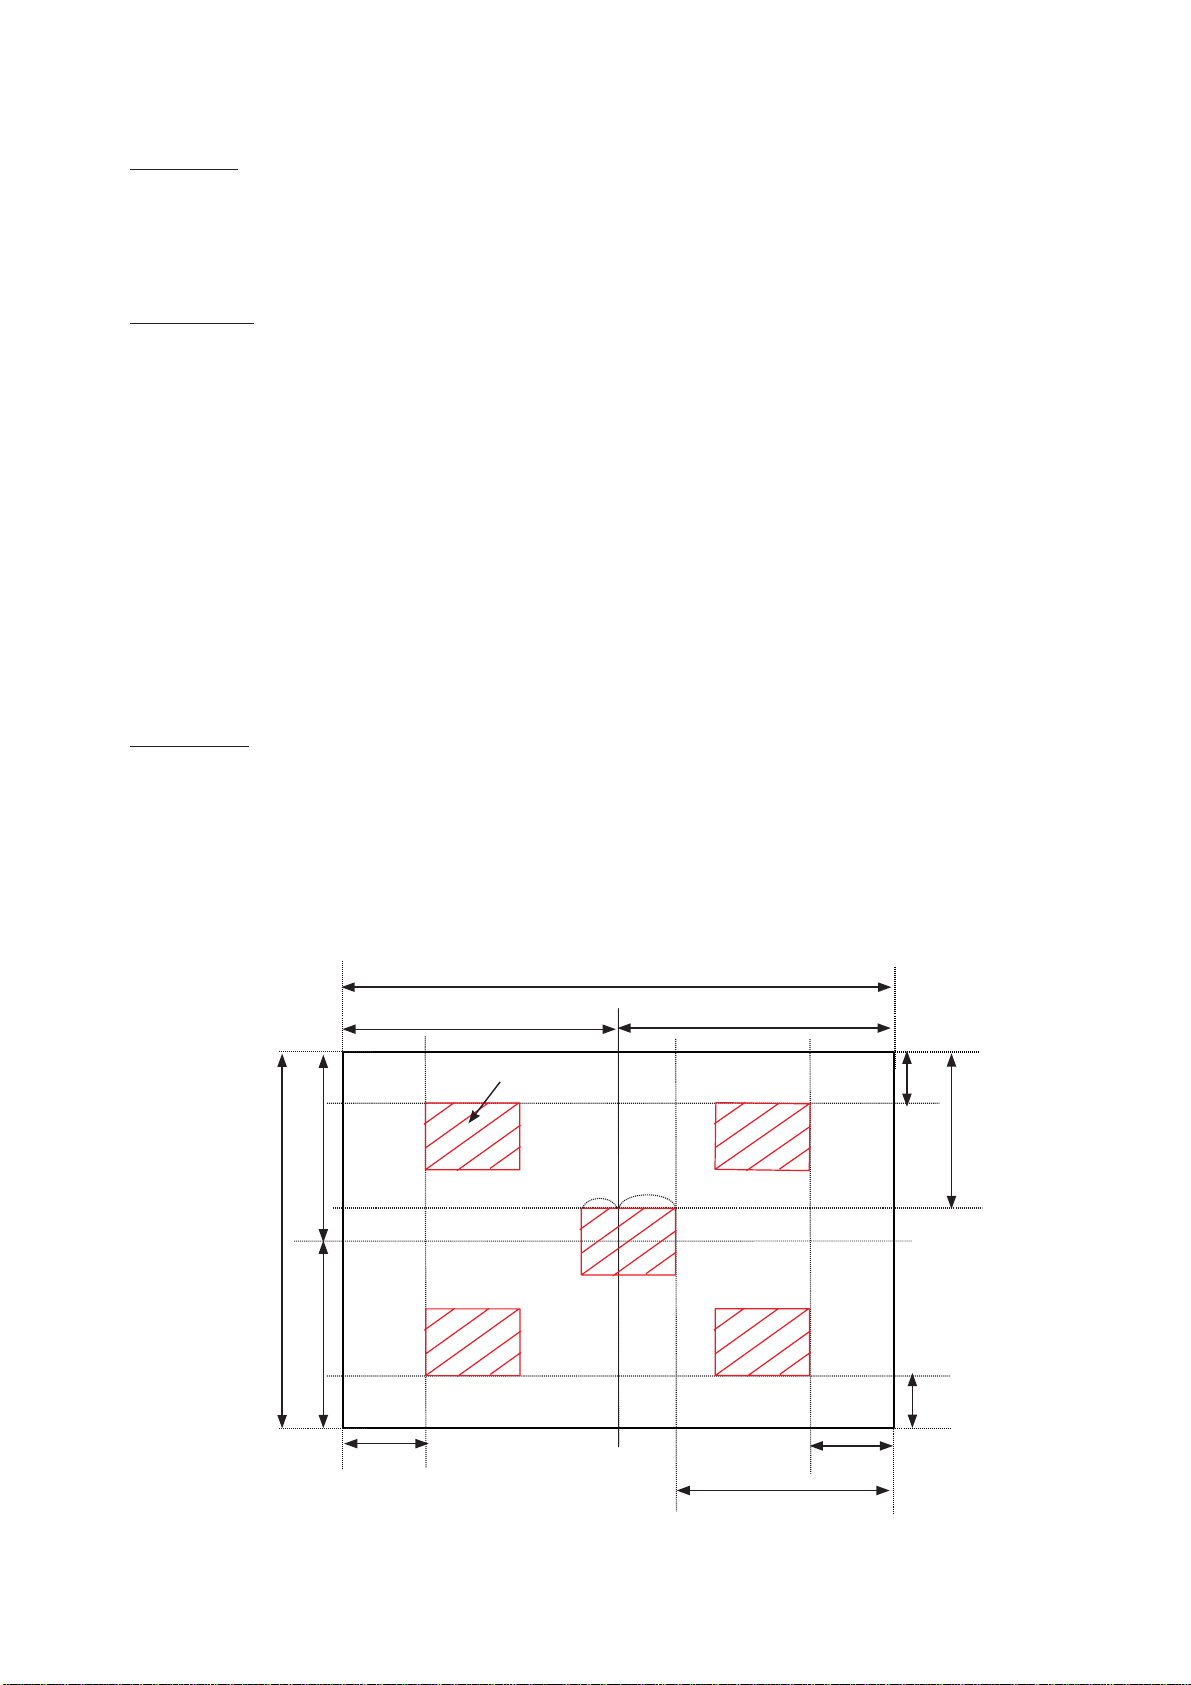
As for the 1st fl attened cardboard box, check the positions which the light viewers fi t in, and cut out
①
at 5 locations (shaded parts/size 154 x 245 mm) as shown below.
(Note) Cutting the shape slightly smaller than the actual size of viewers makes it easier to fi t the positions of
viewers tightly.
1250
625 625
420
154×245
100
145
146
343
the shape
840
420
175
146
175
420
Dimensioned drawing
- A58・AF-S DX 16-85/3.5-5.6G VR -
Page 81
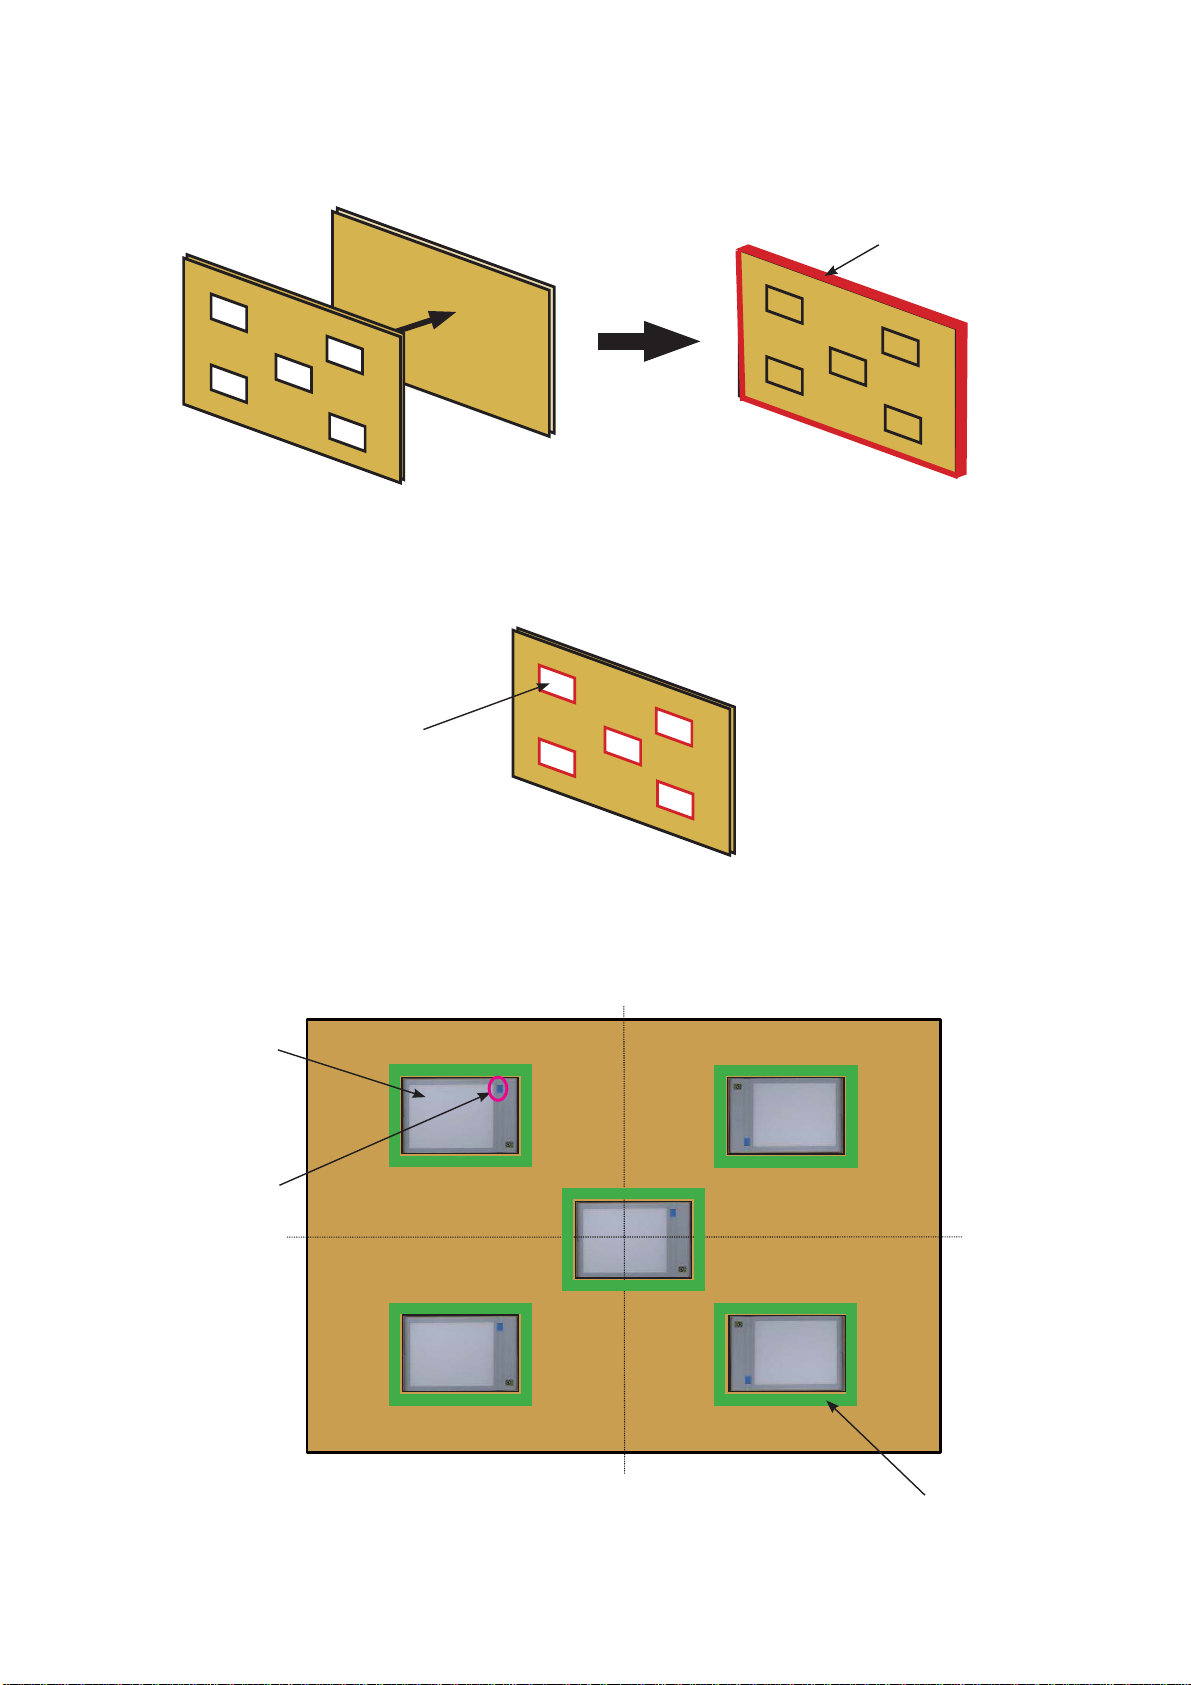
JAA80051-R.3741.A
INC
Put
②
1st cut-out
cardboard
③ As for the above cardboards (② ), cut out the same shape again as the cut-out size (ref. ① ) from the 2nd
the 1st cut-out cardboard ( ① ) and the 2nd fl attened cardboard together as one, and fi x them by taping at
four sides.
2nd fl attened cardboard
Tape
fl attened cardboard for each viewer at fi ve places.
Cut out at 5 places
Fit the viewers in the created boards so that each viewer's switch is positioned as below.
④
⑤ Reinforce the edges of cut-out parts with double-stick tape.
Viewer
Switch
Double-stick tape (at 5 places)
- A59・AF-S DX 16-85/3.5-5.6G VR -
Page 82
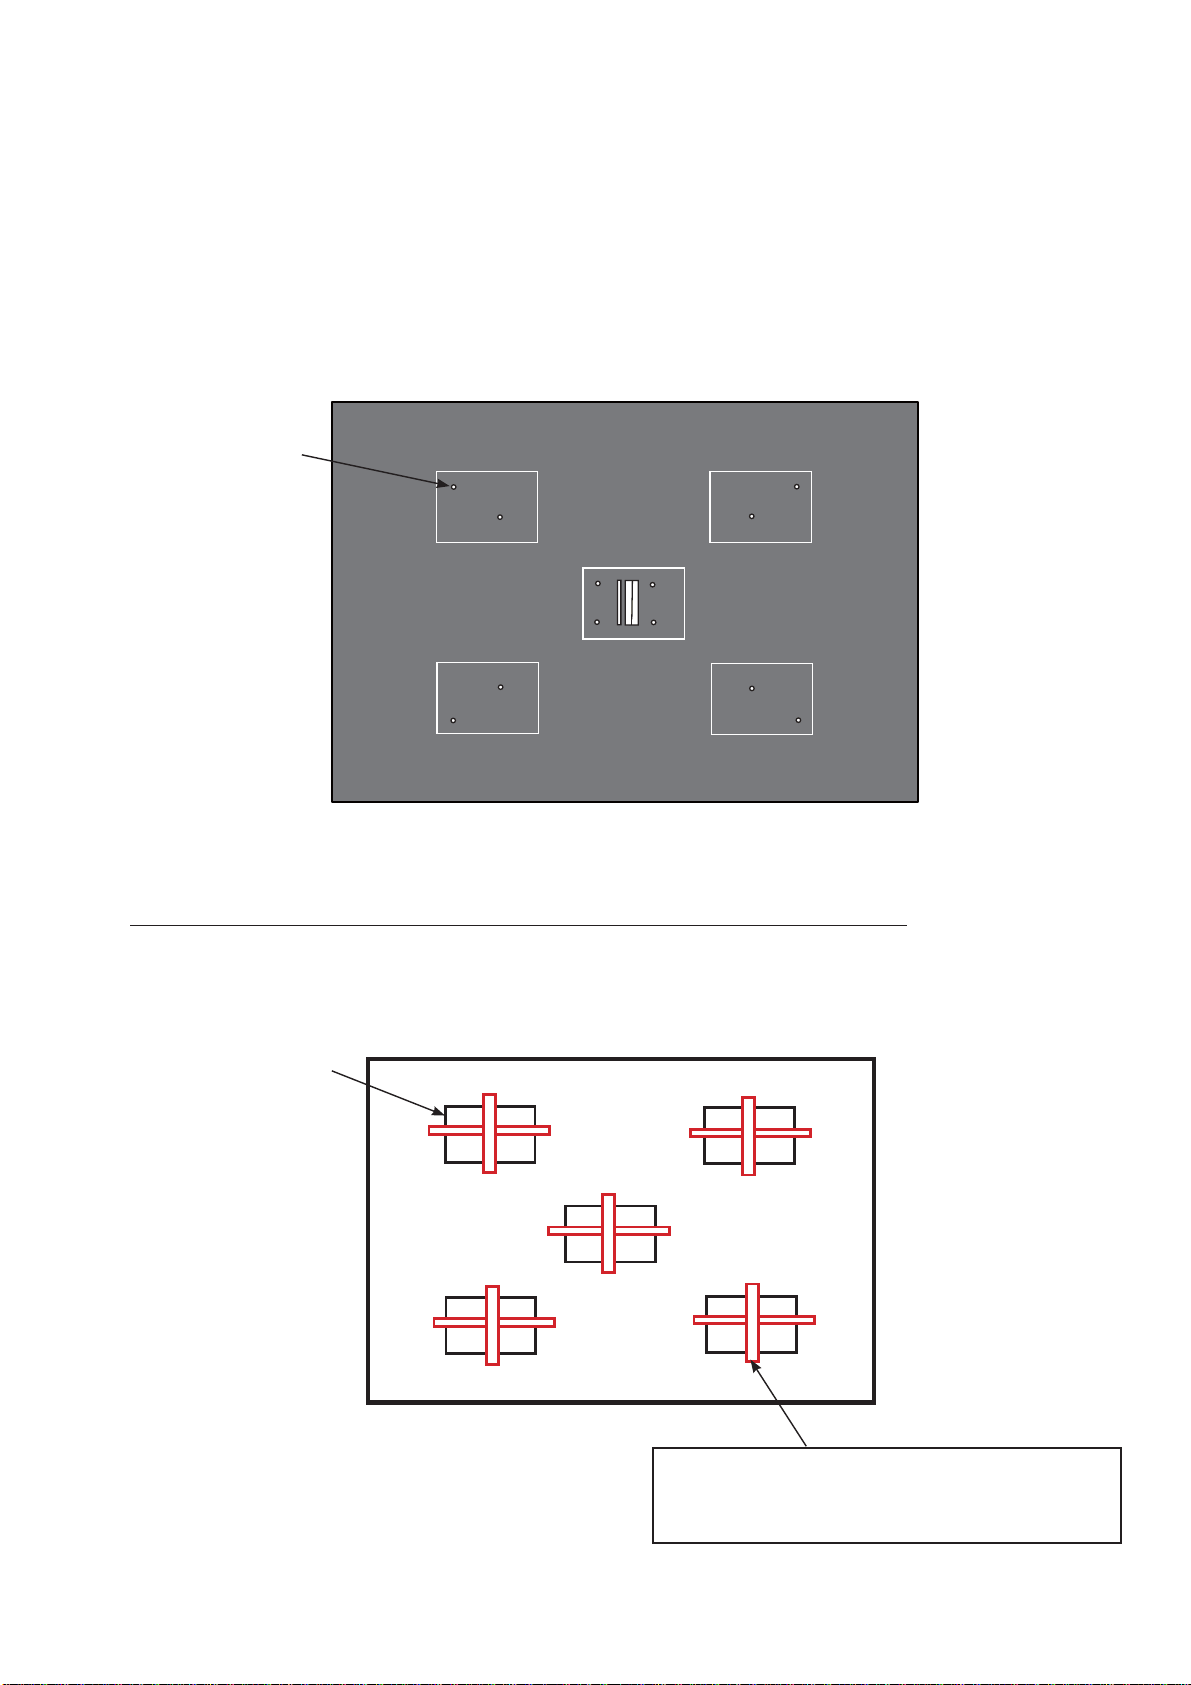
JAA80051-R.3741.A
INC
Light up the viewers. Set and attach the alignment chart (J19134) so that all the pinholes are located on the
⑥
viewer.
If the setting board is larger than the alignment chart, blacken the area around the setting board with black
spray, etc, after attaching the chart.
Caution:
T o prevent the chart from being slackened around the pinholes, secure the chart by adhering the double-stick tape
around the pinholes.
Pinhole
4. Prevent Viewers from falling off (In this document, 2-mm width Velcro tape is used.)
After viewers are put in position, secure them with Velcro tape (hook and loop fastener) on the back of the
cardboard to prevent viewers falling off.
Viewer
To prevent viewers falling off, attach Velcro tape
on the back of the cardboard. Here in this document, 2mm-width tape is used.
- A60・AF-S DX 16-85/3.5-5.6G VR -
Page 83
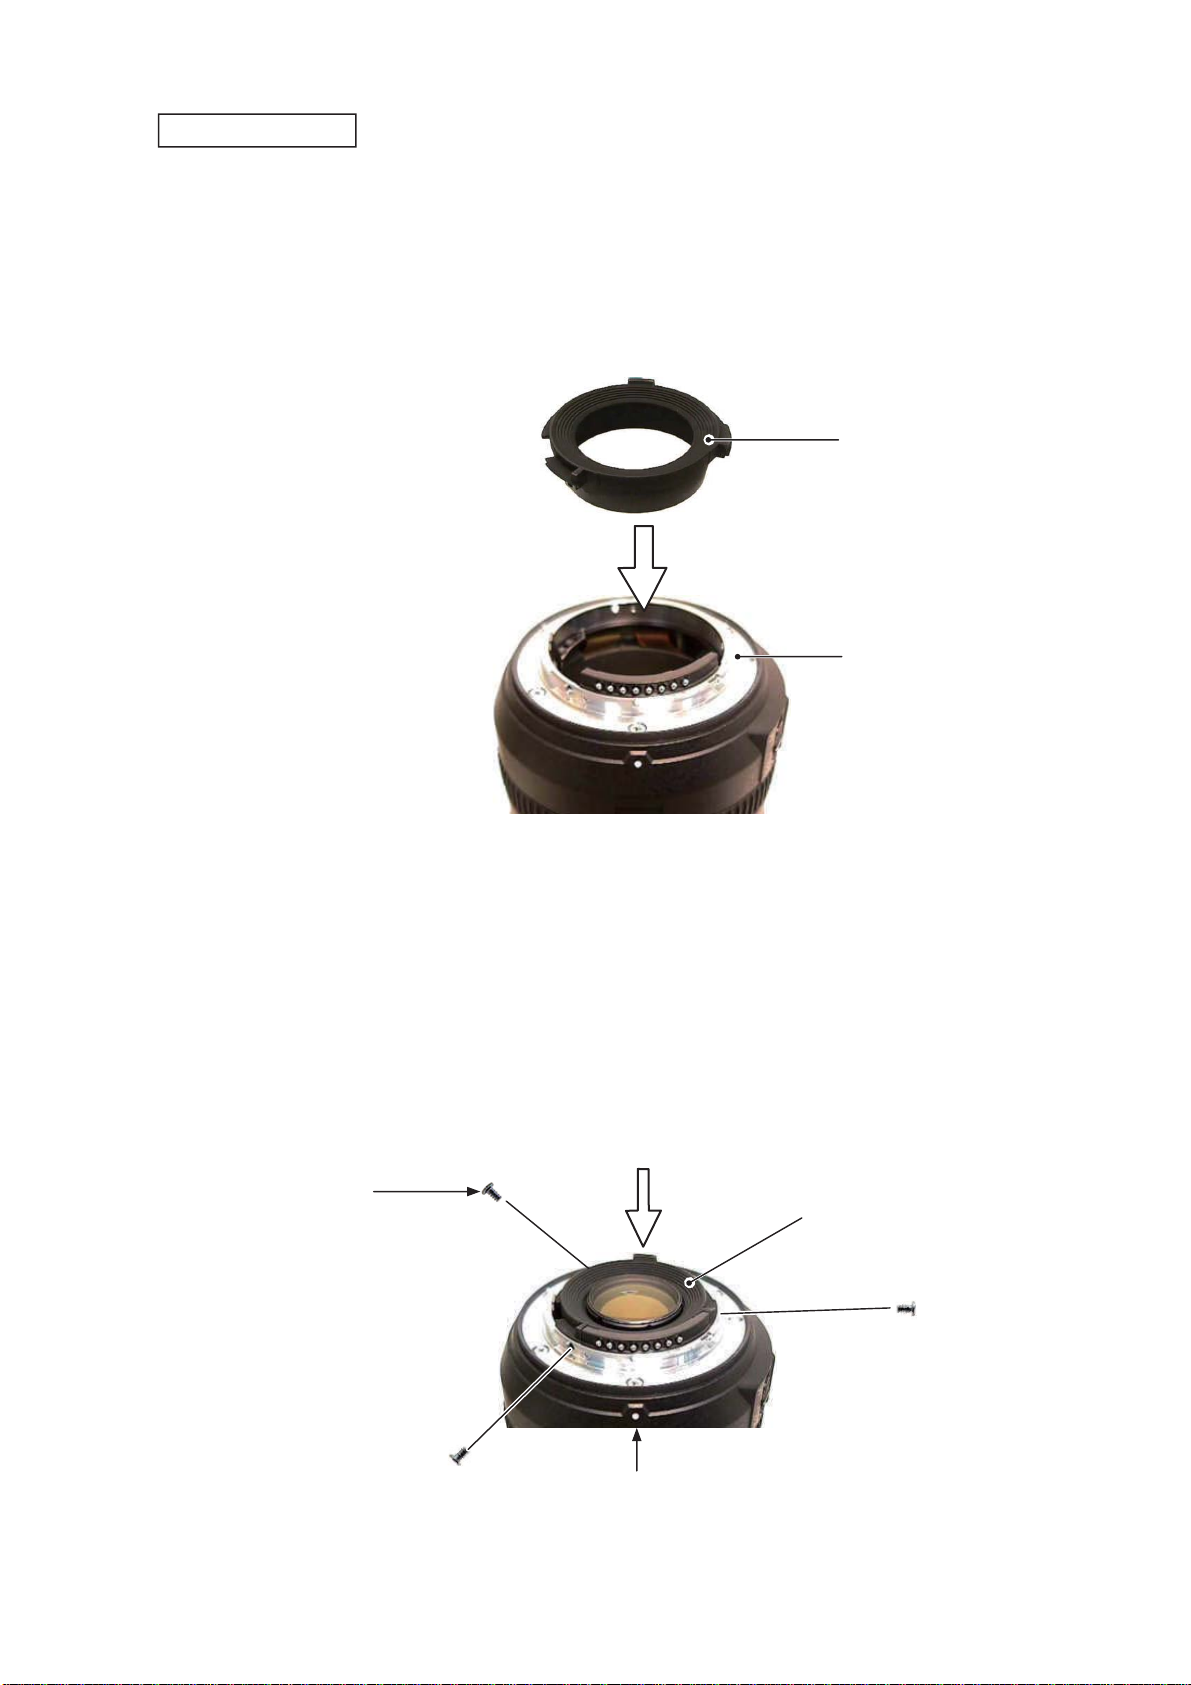
Rear cover ring
INC
Mount the rear cover ring (#39) on the bayonet mount unit (B30).
・
JAA80051-R.3741.A
#39
B30
While pressing the rear cover ring (#39) from above, tighten the three screws (#118) in numeric order (①,
・
, and ③).
②
②
#118×3
#39
①
- A61・AF-S DX 16-85/3.5-5.6G VR -
Index
③
Page 84
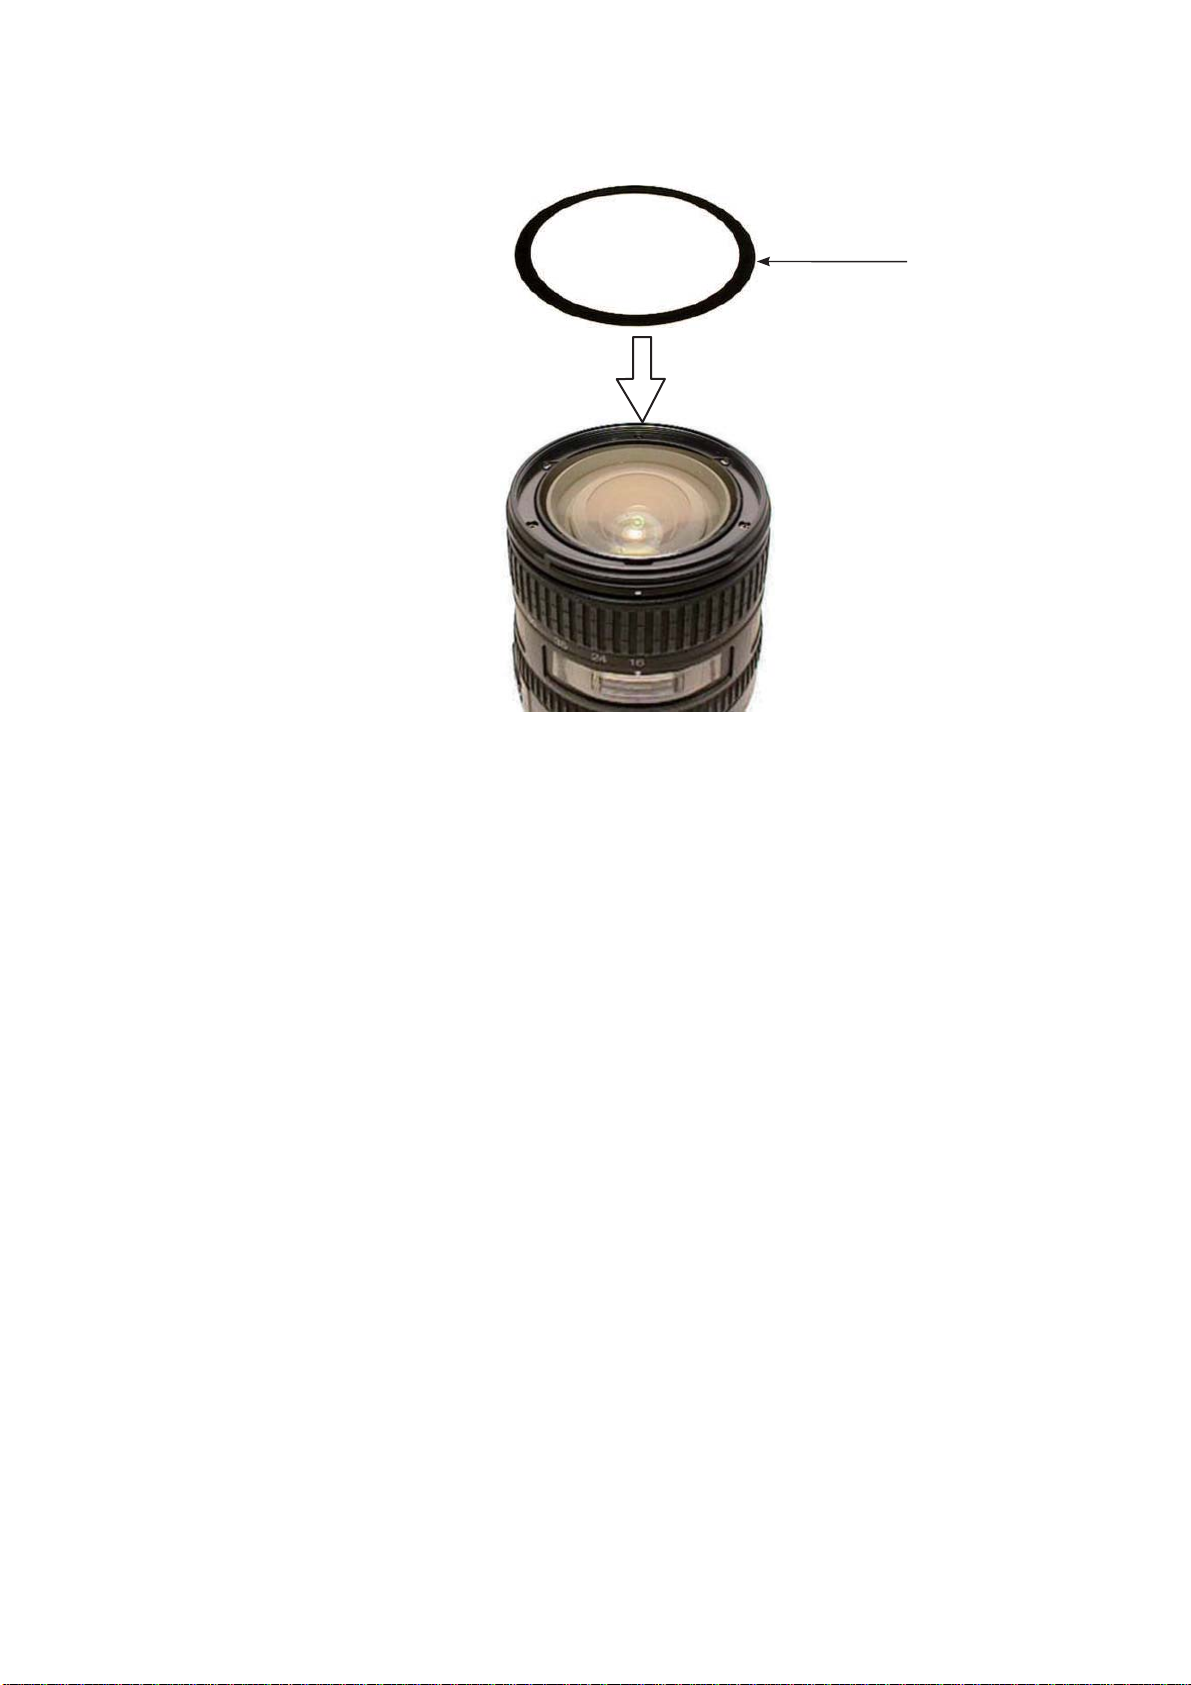
Adhere the sheet (#60) on the fi lter ring.
INC
JAA80051-R.3741.A
#60
- A62・AF-S DX 16-85/3.5-5.6G VR -
Page 85
JAA80051-R.3741.A
INC
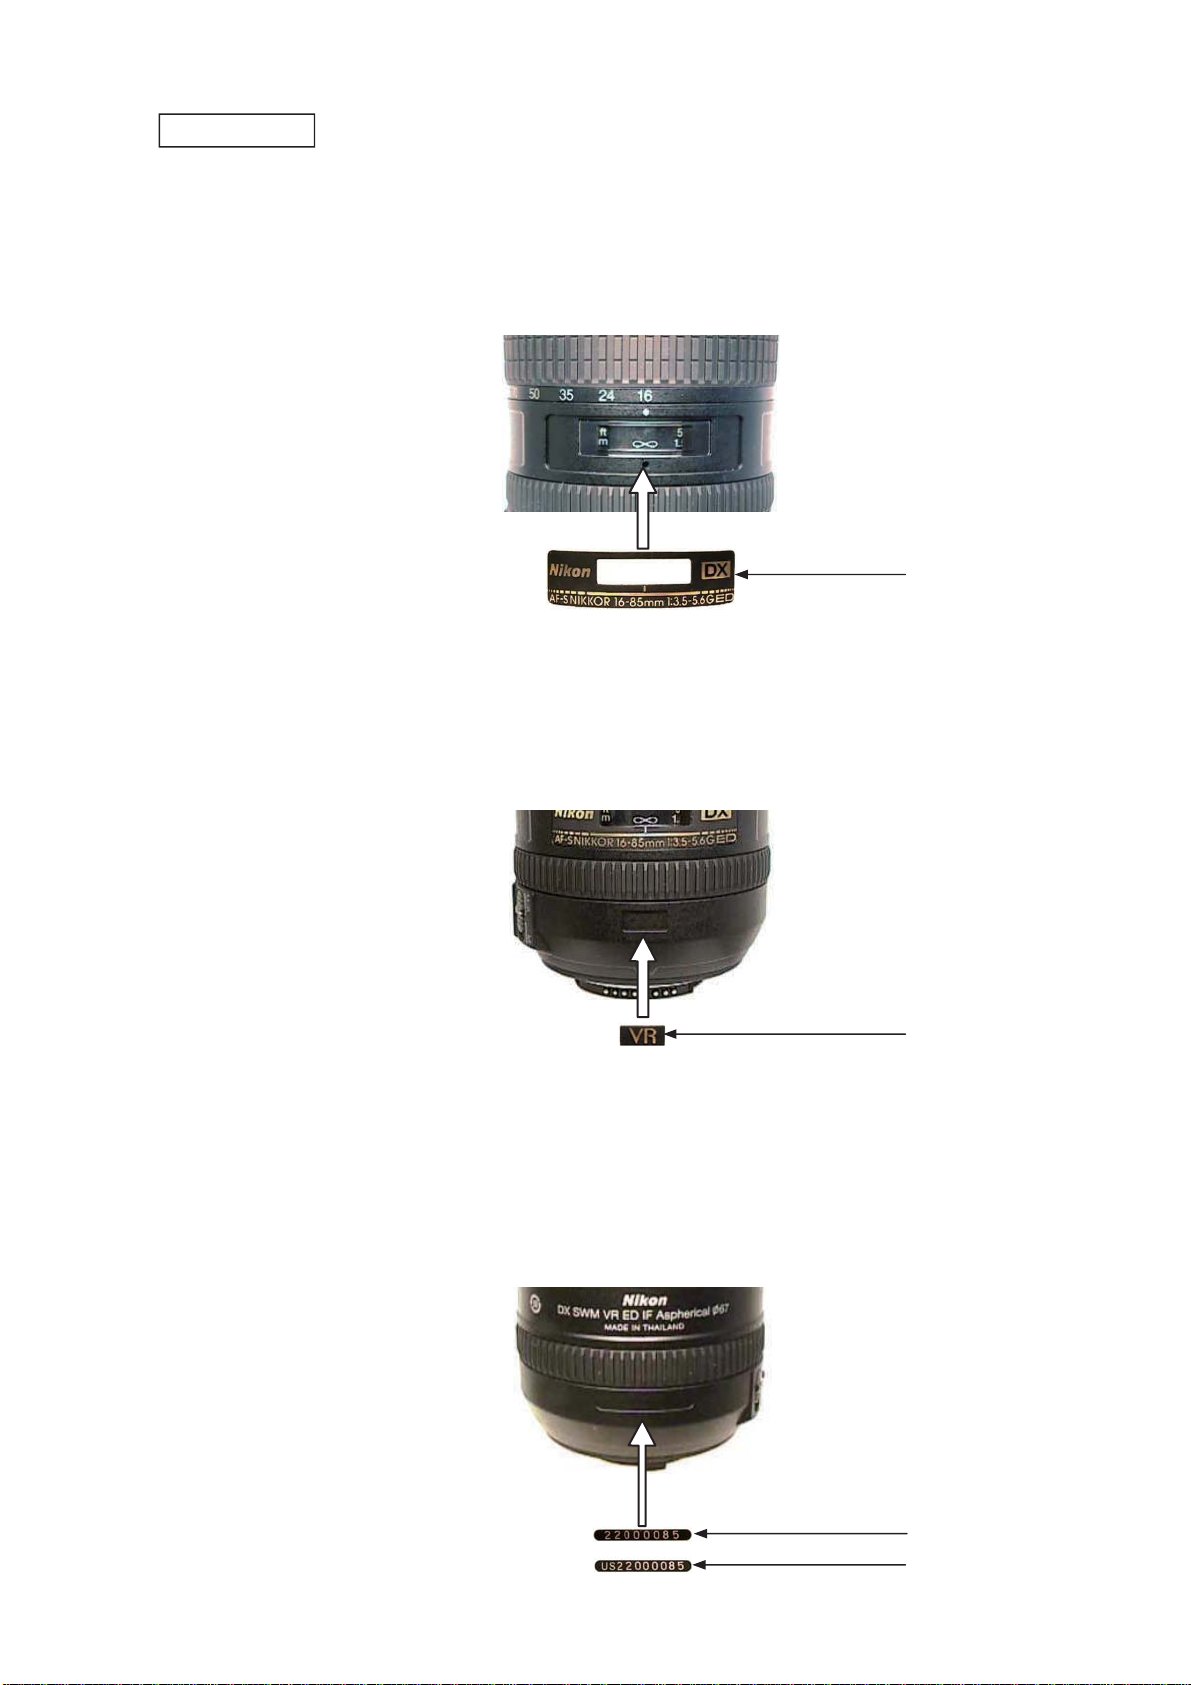
Name plate
Peel off the tape that attaches the window (#76) temporarily. Peel off the backing paper of the name plate
・
(#68) and attach [#68].
#75
Peel off the backing paper of VR name plate (#69) and attach [#69].
・
#69
Peel off the backing paper of the serial number label (#168 or #169), and attach [#168 or #169].
・
#168
#169
- A63・AF-S DX 16-85/3.5-5.6G VR -
Page 86
JAA80051-R.3741.A
INC
Preparation for Inspection & Adjustment
New tool
★:
● In case of replacing the main PCB unit or SWM unit, etc, be sure to make the adjustments by using the
adjustment software (★J18444).
Required device:
・Single output rated voltage power supply: 1 unit (6.0V 3.0A)
・Oscilloscope: 1 unit For inspecting lens driving time
・AF-I communication box (J15306-1): 1 unit
・AF-I communication adapter (J15307): 1 unit
● When the main PCB is replaced, be sure to perform "Writing of FLASH-ROM fi xed elec. adj. values".
AF-S DX 16-85/3.5-5.6G VR Inspection and adjustment program (★J18444)
The below hardware requirements are necessary for installing the program on a computer.
Ensure them before installation.
PC IBM PC/AT compatible
OS Windows XP Home Edition, Windows XP Professional, Windows 2000
CPU Pentium Ⅱ 266MHz ~ Pentium Ⅳ 2GHz
RAM (Memory) 32MB or more
HD 6 MB-or-more free space is necessary when installation
Monitor resolution 800×600 or more pixels
Interface Serial interface
※ USB interface cannot be used.
As long as the above requirements are met, either desktop or notebook PC is available.
- A64・AF-S DX 16-85/3.5-5.6G VR -
Page 87
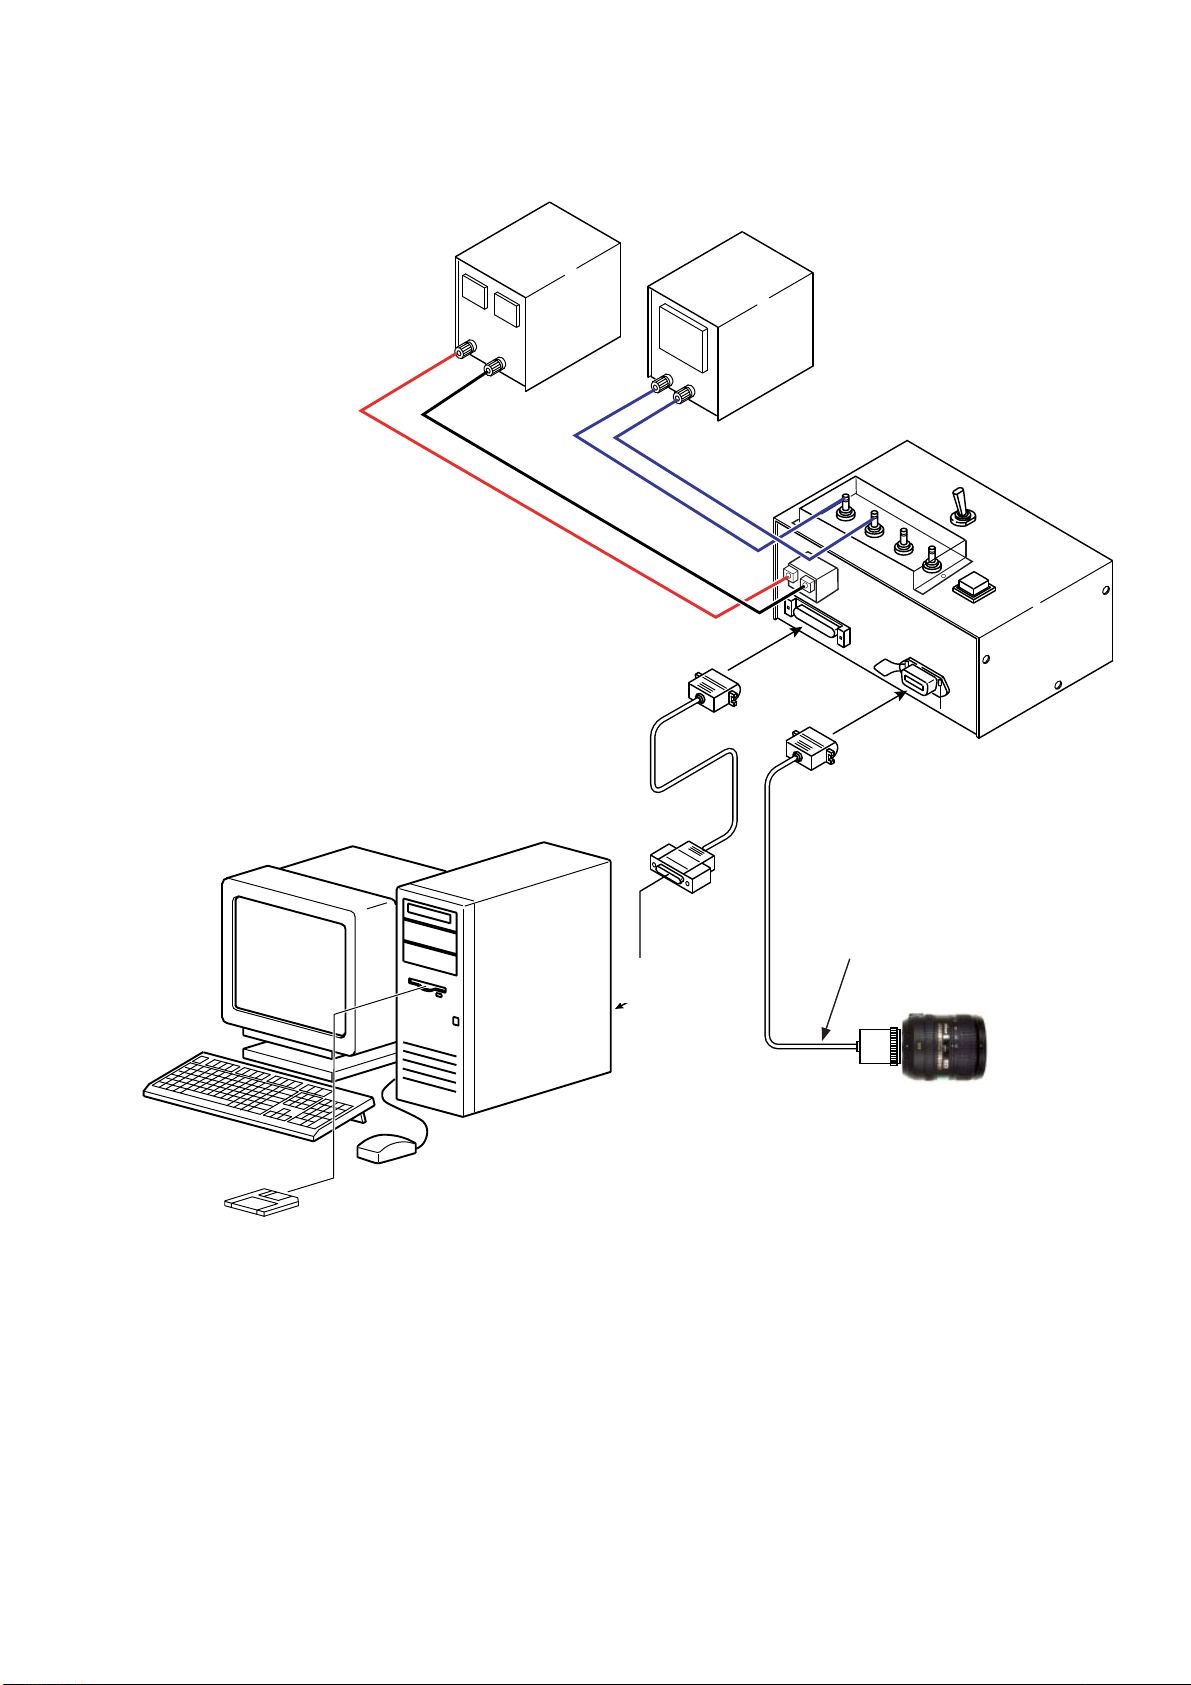
【System confi guration】
INC
Constant-voltage power supply
(Set voltage: 6V)
(+)
JAA80051-R.3741.A
New tool
★:
(-)
If the RS232C terminal of PC is a 9-pin type,
connect it by using the 25-pin/9-pin conversion
connector. This connector is NOT supplied as RJ,
so use commercial products on the market.
Oscilloscope
AF-I communication box
(J15306-1)
AF-I communication adapter
(J15307)
To RS232C
terminal
AF-S DX 16-85 VR
Inspection & adjustment software
(★J18444
)
AF-S DX 16-85 VR
PC:
As long as PC is IBM PC/AT compatible,
any CPU type is available.
- A65・AF-S DX 16-85/3.5-5.6G VR -
Page 88
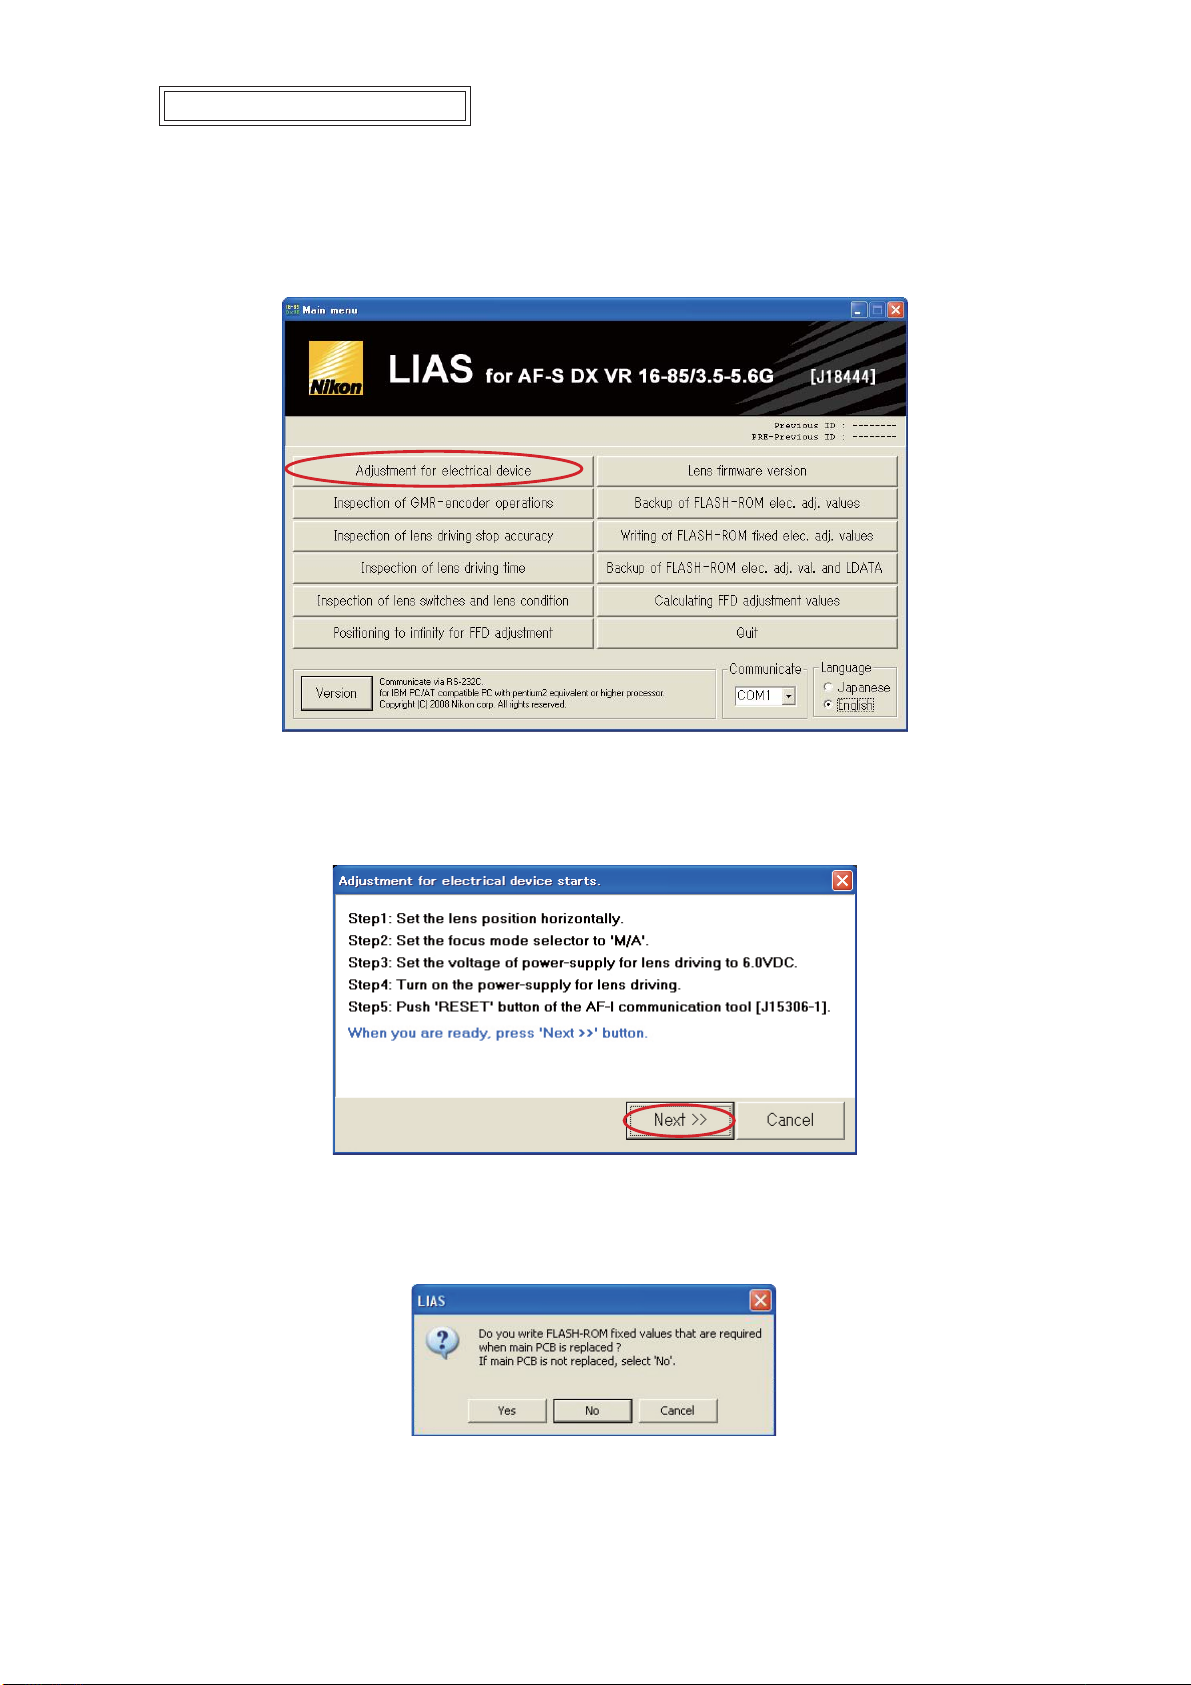
Adjustment for electrical device
INC
●
When the main PCB unit or SWM unit is replaced, be sure to make this adjustment.
JAA80051-R.3741.A
・
Click "Adjustment for electrical device" on the main menu
・
Follow the instructions on the screen for preparation. Then click "Next".
.
Click "Yes" if the main PCB was replaced, while click "No" if it was NOT replaced.
・
Clicking "Yes" goes on to "Writing of FLASH-ROM elec.adj.values" (on Page A83).
- A66・AF-S DX 16-85/3.5-5.6G VR -
Page 89
JAA80051-R.3741.A
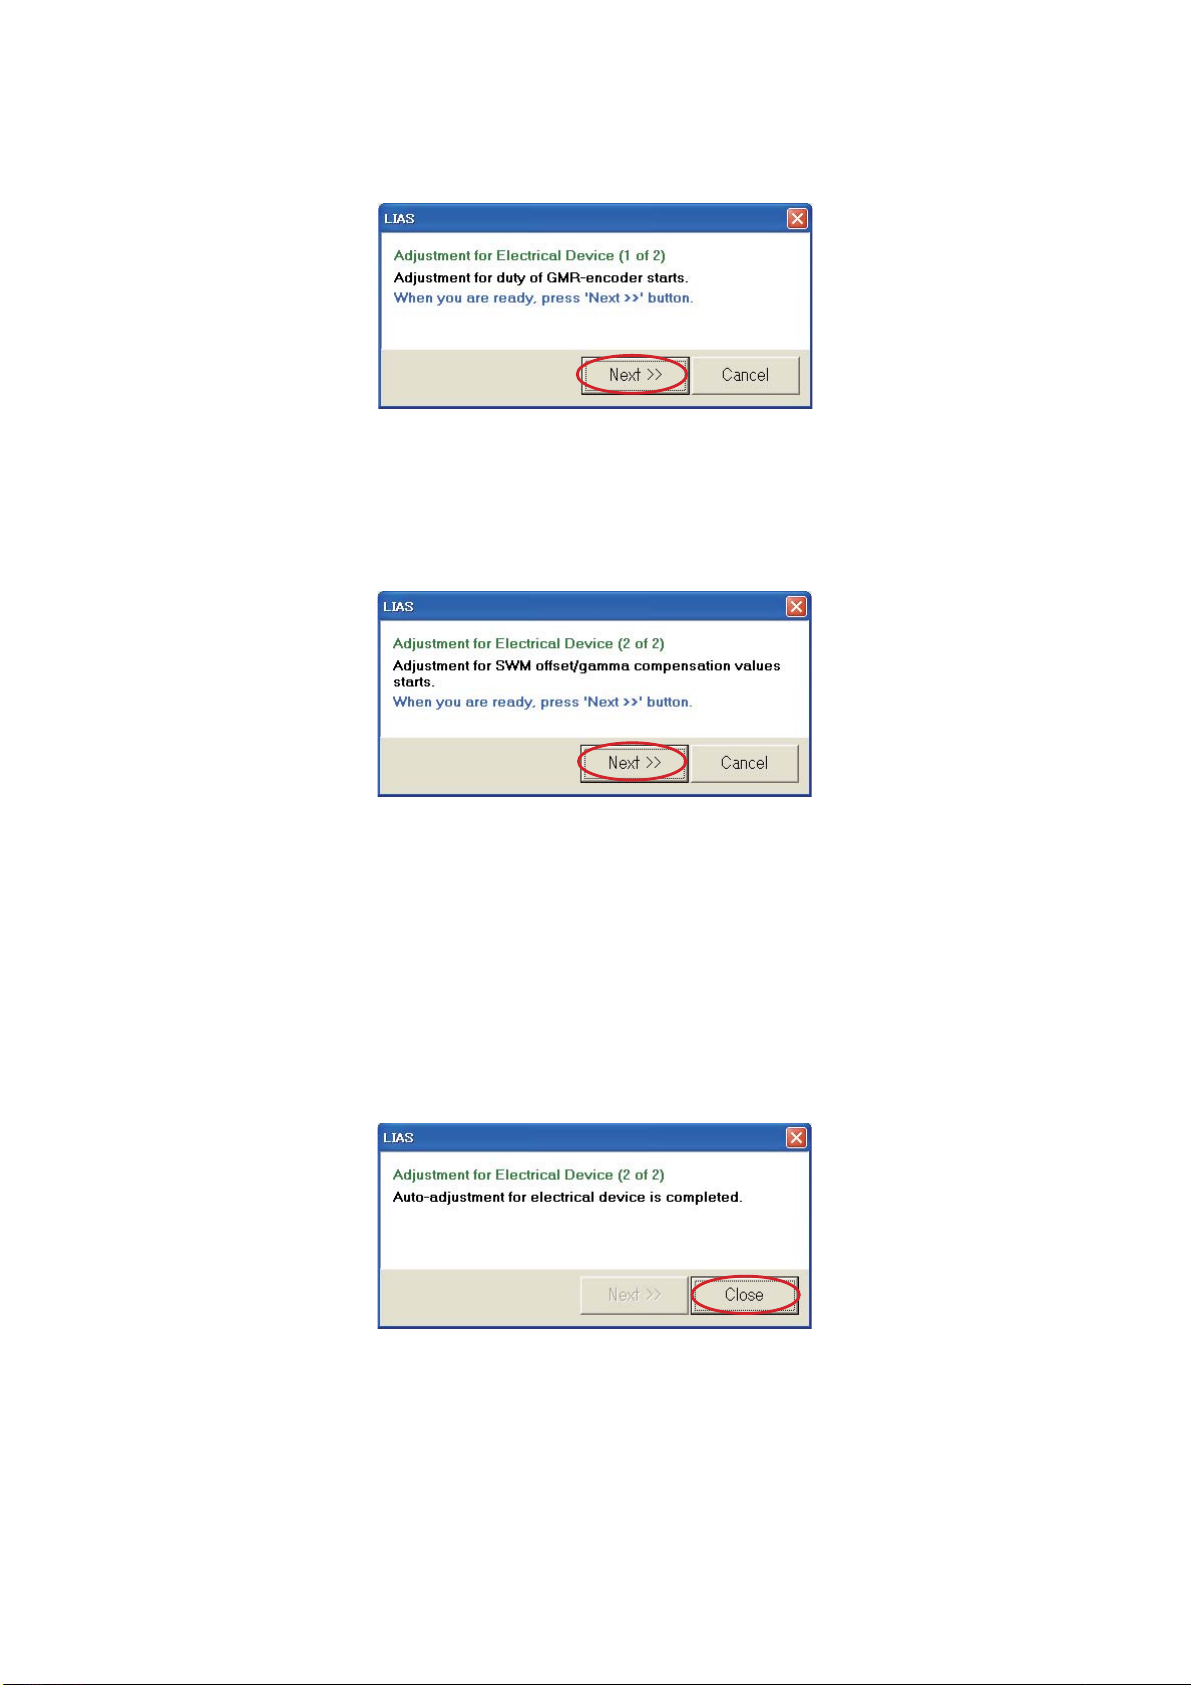
INC
・
Click "Next"
・
Click "Next"
.
.
・
When adjustment is completed, click “Close” to end the procedure.
- A67・AF-S DX 16-85/3.5-5.6G VR -
Page 90
Inspection of GMR-encoder operations
INC
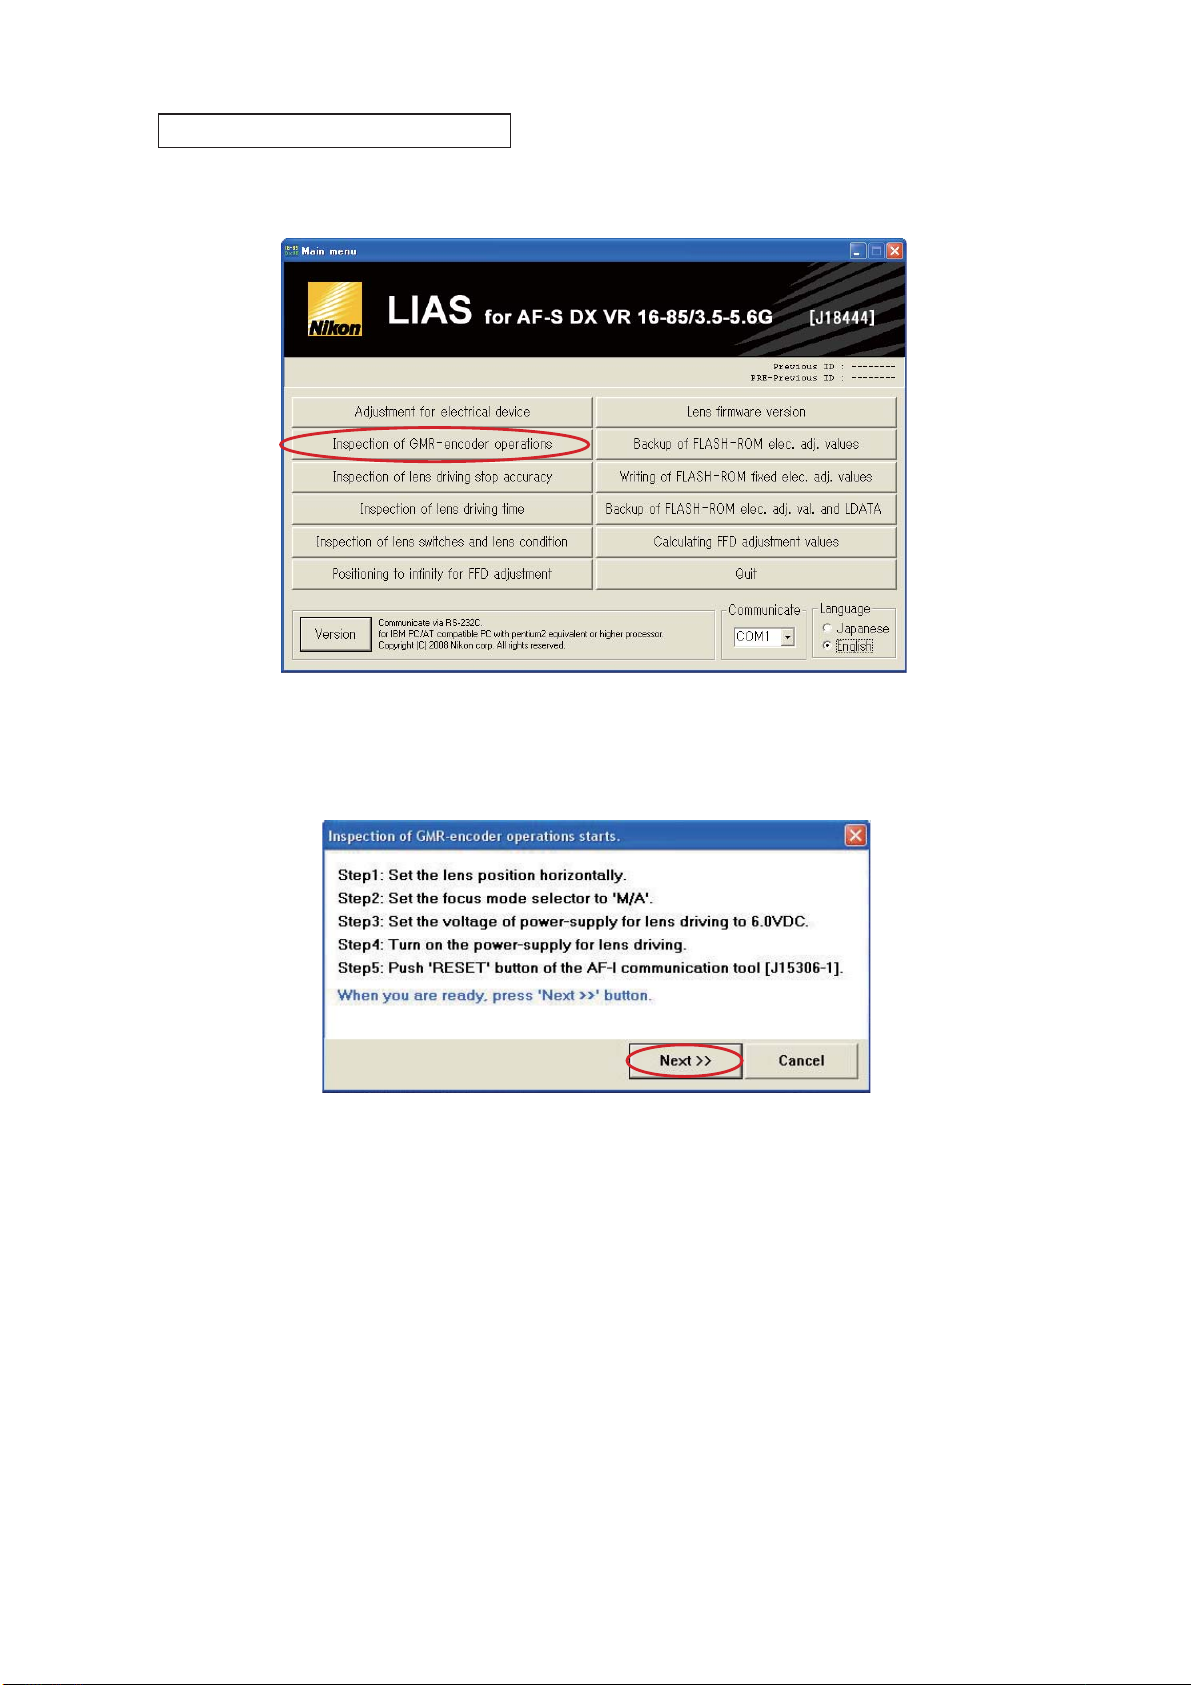
Click "Inspection of GMR-encoder operations" on the main menu.
・
JAA80051-R.3741.A
Follow the instructions on the screen. When prepared, click "Next".
・
- A68・AF-S DX 16-85/3.5-5.6G VR -
Page 91
JAA80051-R.3741.A
INC
・
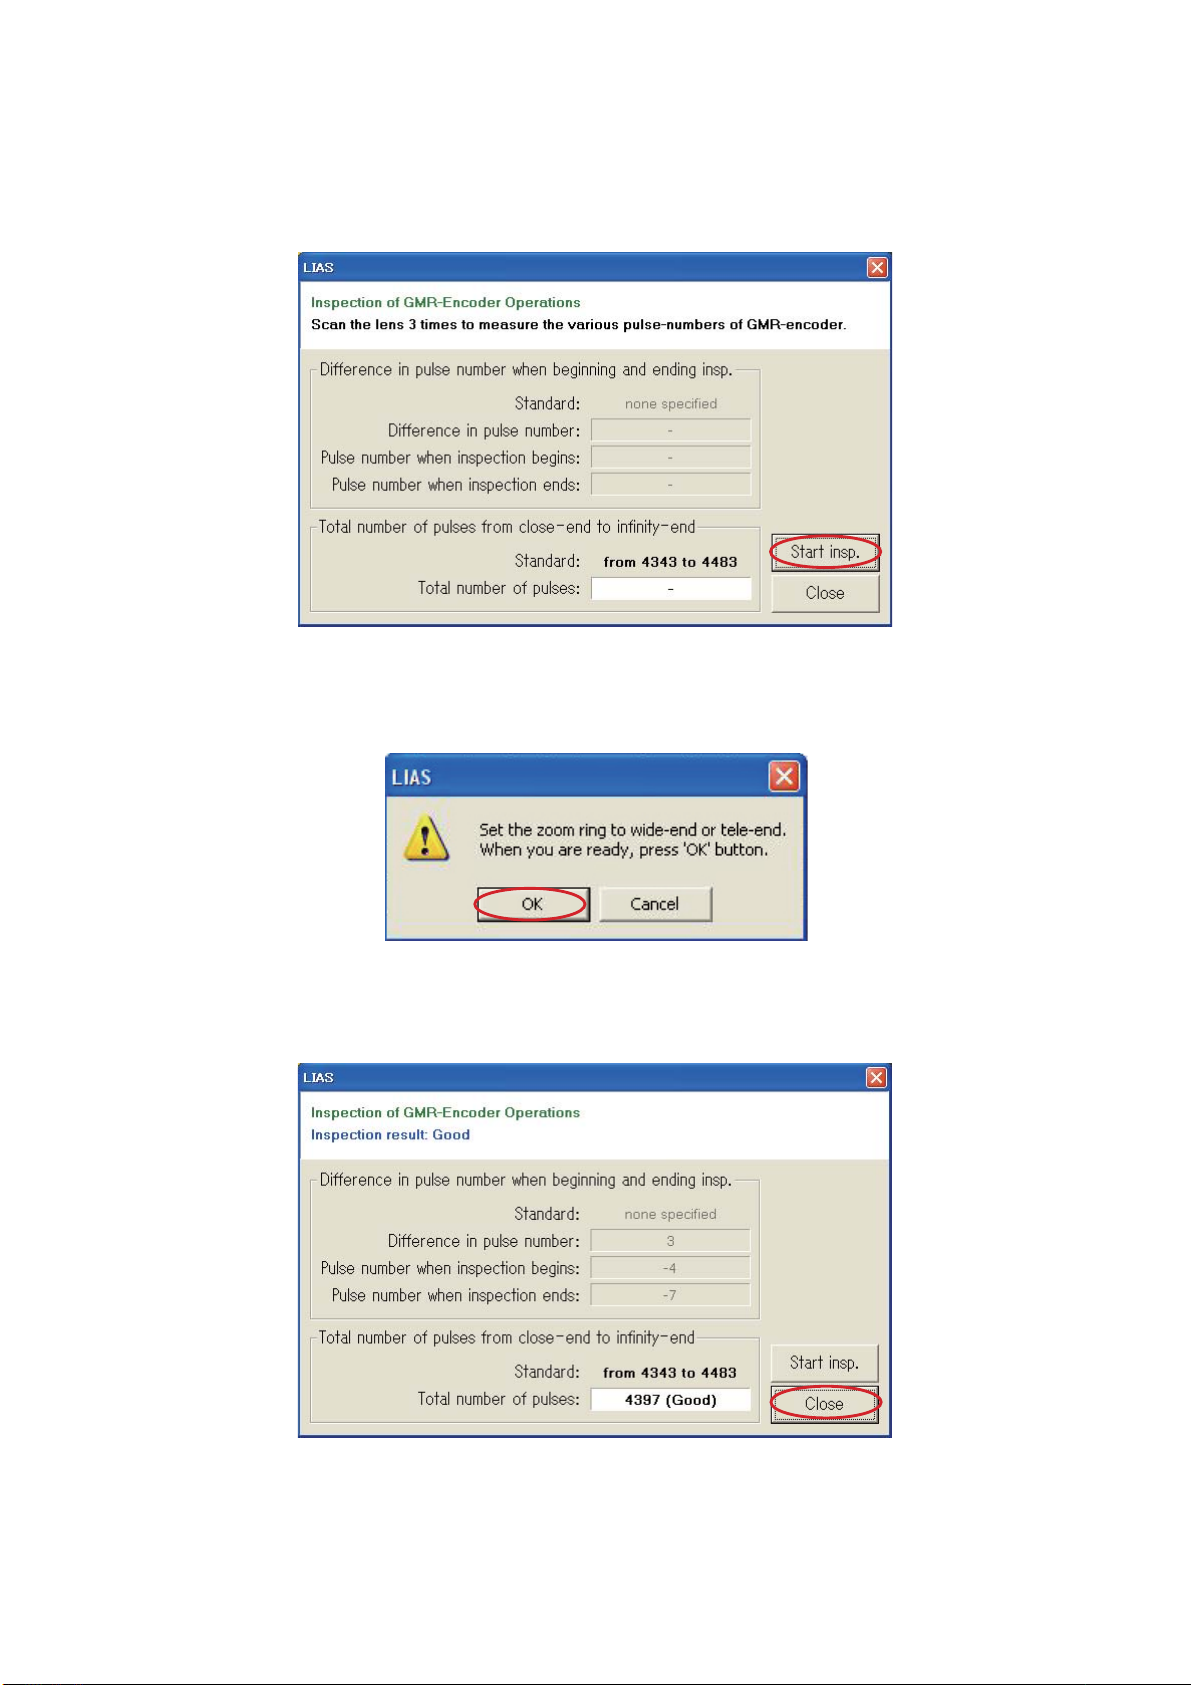
Click "Start insp.".
Caution:If the zoom ring is rotated while the lens scanning is driven, the pulse shows an abnormal value.
Do NOT touch the zoom ring during operations.
Set the zoom ring to WIDE-end or TELE-end, and click "OK".
・
・
If "Inspection result" shows "Good", click "Close".
< Standard > Total pulses
:
4343 - 4483 PULSE(S)
- A69・AF-S DX 16-85/3.5-5.6G VR -
Page 92
JAA80051-R.3741.A
INC
Inspection of lens driving stop accuracy
●
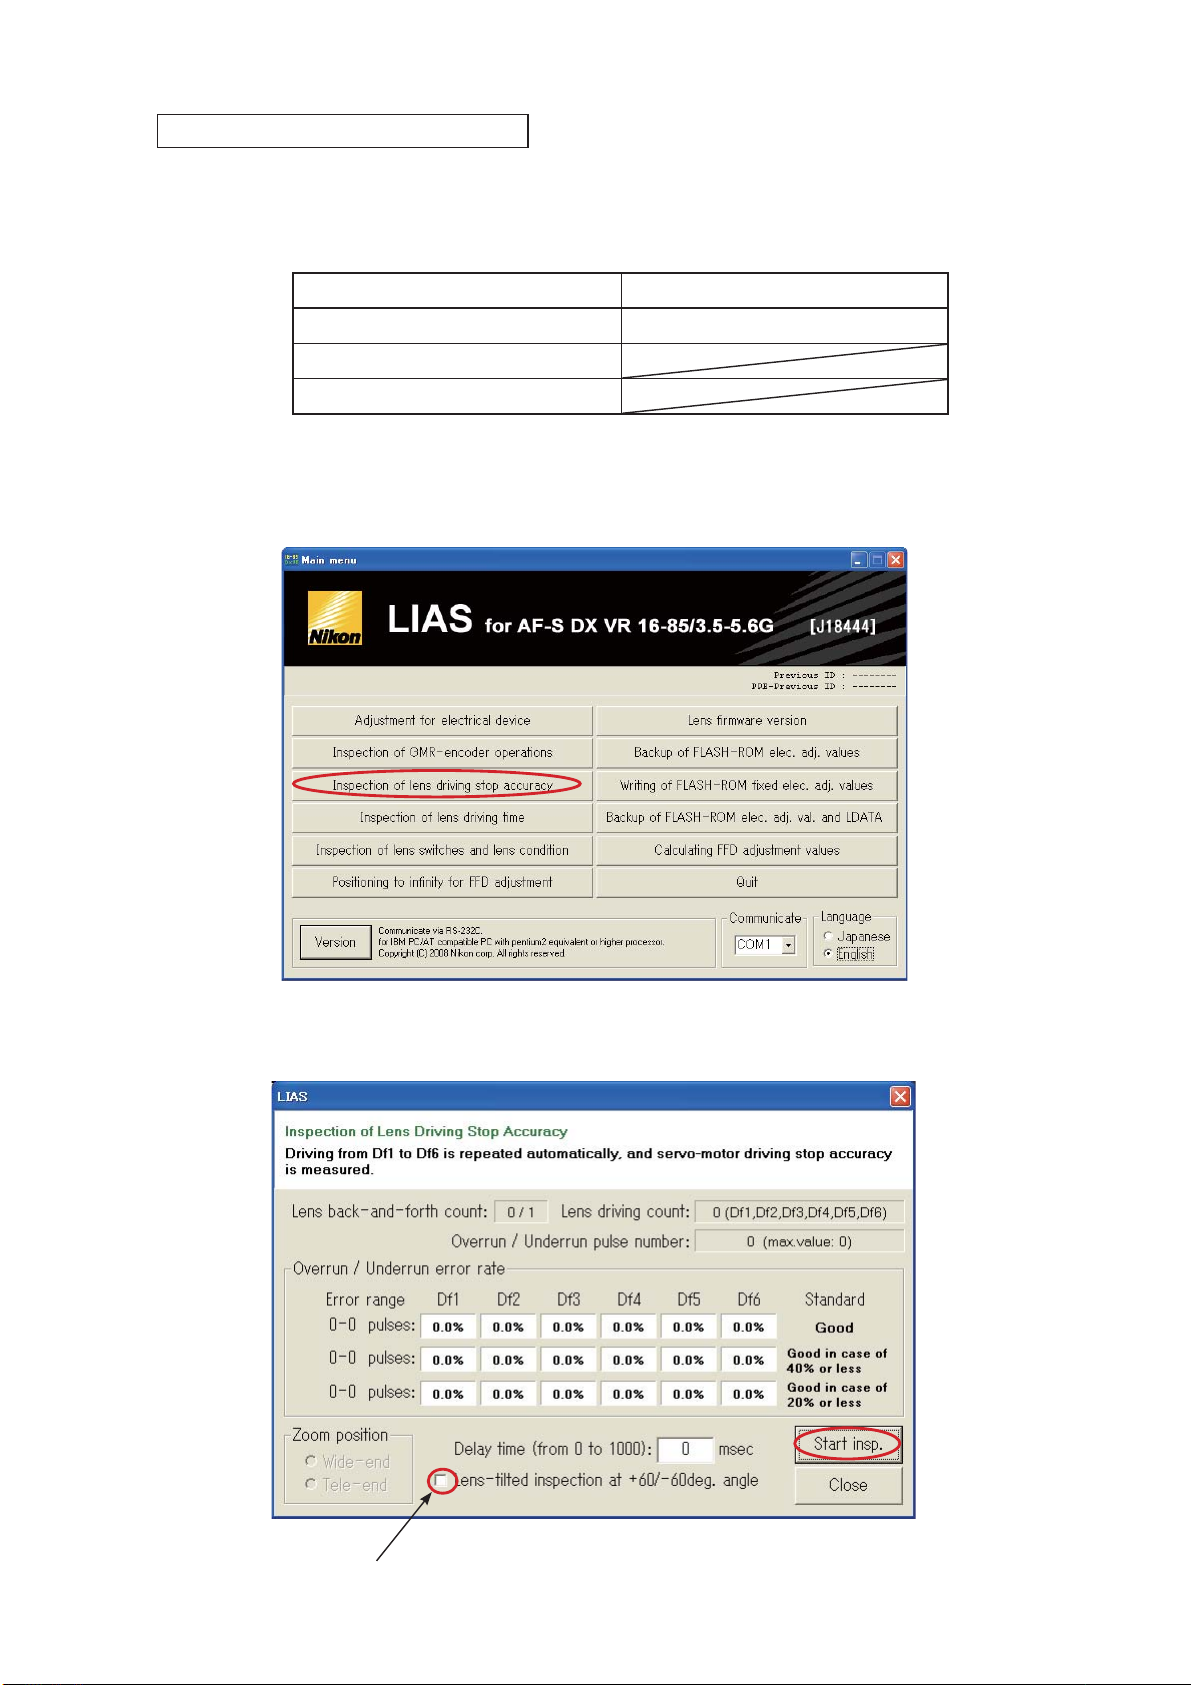
Make the inspections by focal length 16mm (W) or 85m (T) at the following fi ve lens positions.
(Lens position in inspecting)
Lens position Index position
Horizontal lens position Index facing (1)
(4) Front lens group 60° angle upward
(5) Front lens group 60° angle downward
・
Click "Inspection of lens driving stop accuracy" on the main menu
up / (2) right / (3) left
.
・
Click "Start insp.".
Tick here when measuring with the front lens group facing 60° angle up/downward.
- A70・AF-S DX 16-85/3.5-5.6G VR -
Page 93
JAA80051-R.3741.A
INC
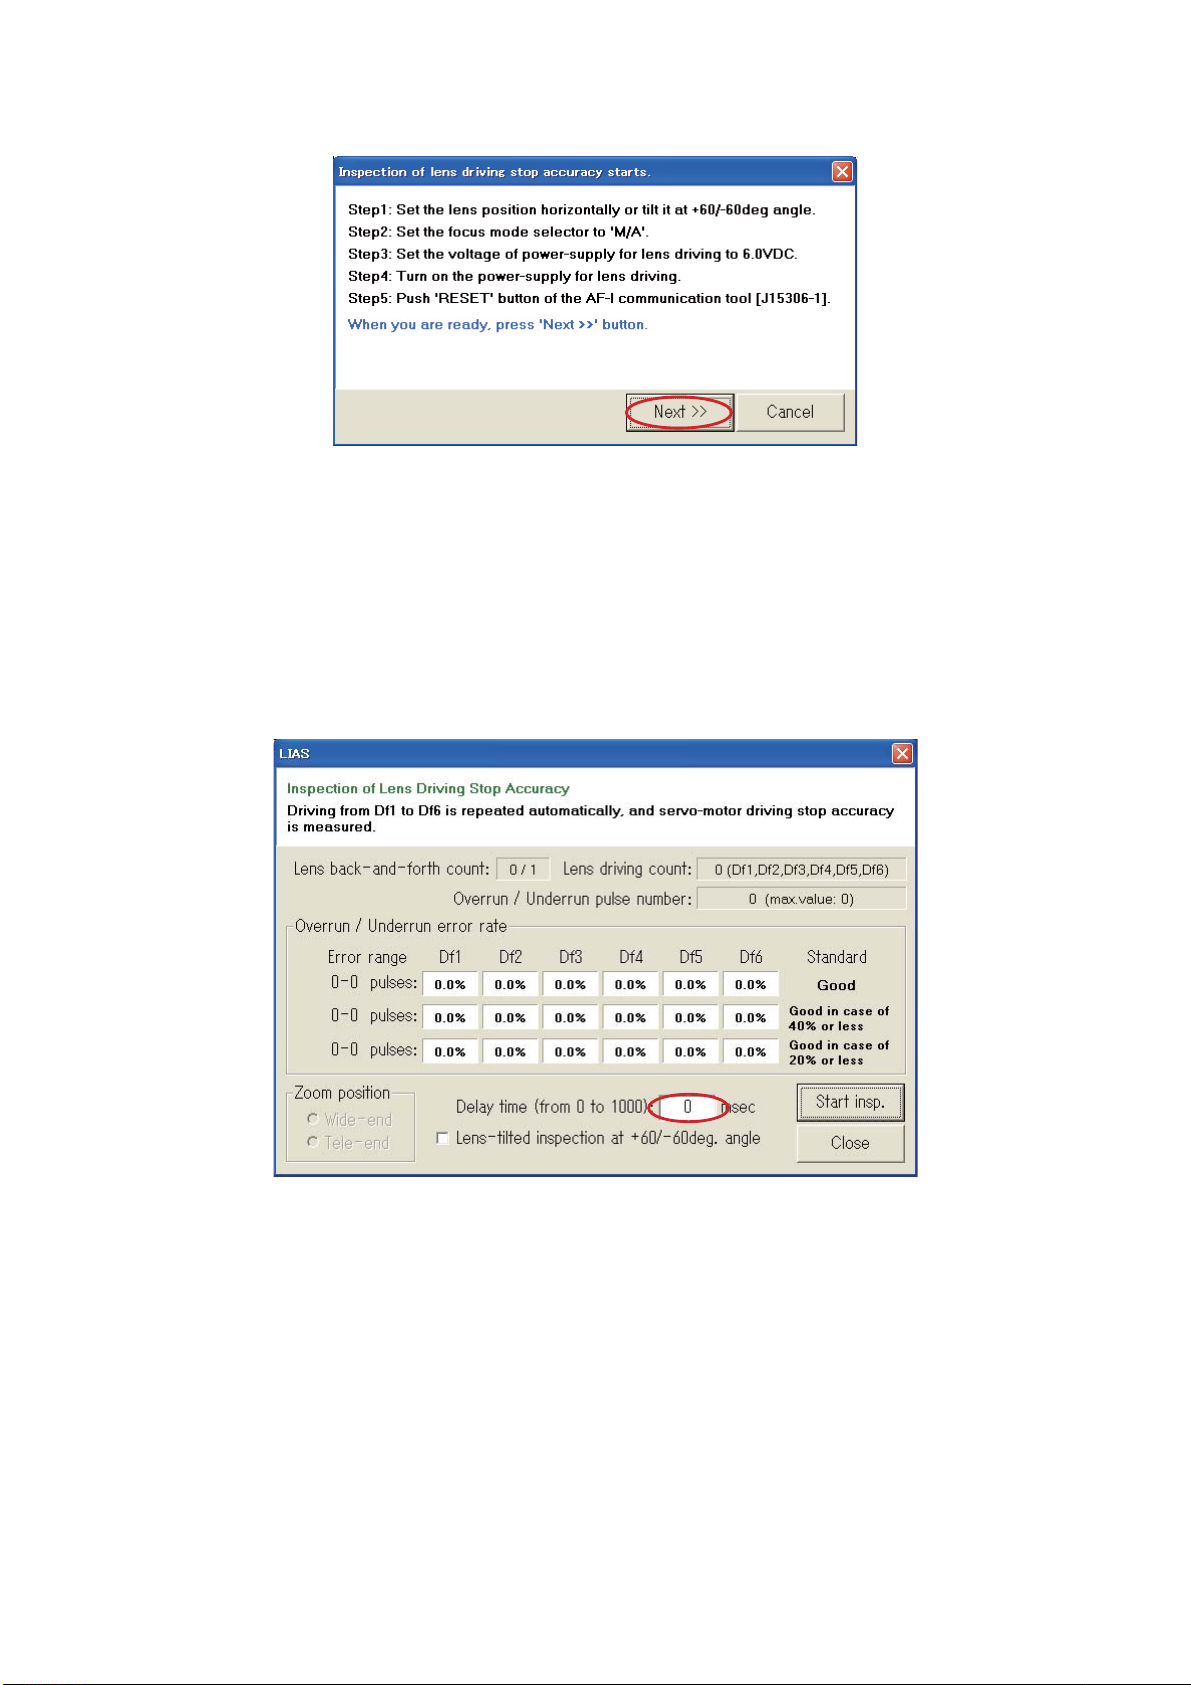
・
Follow the instructions on the screen. When prepared, click "Next".
If the lens stops, input a numeric number into "Delay time (from 0 to 1000 msec.) so that the lens does
・
NOT stop.
Caution: The value of "Delay time" is set by the adjustment software. So, as far as the lens does not
stop during the inspection of "Lens Driving Stop Accuracy", any value can be input without
problem.
However, the larger the value of "Delay time" gets, the longer the inspection time becomes.
- A71・AF-S DX 16-85/3.5-5.6G VR -
Page 94
・
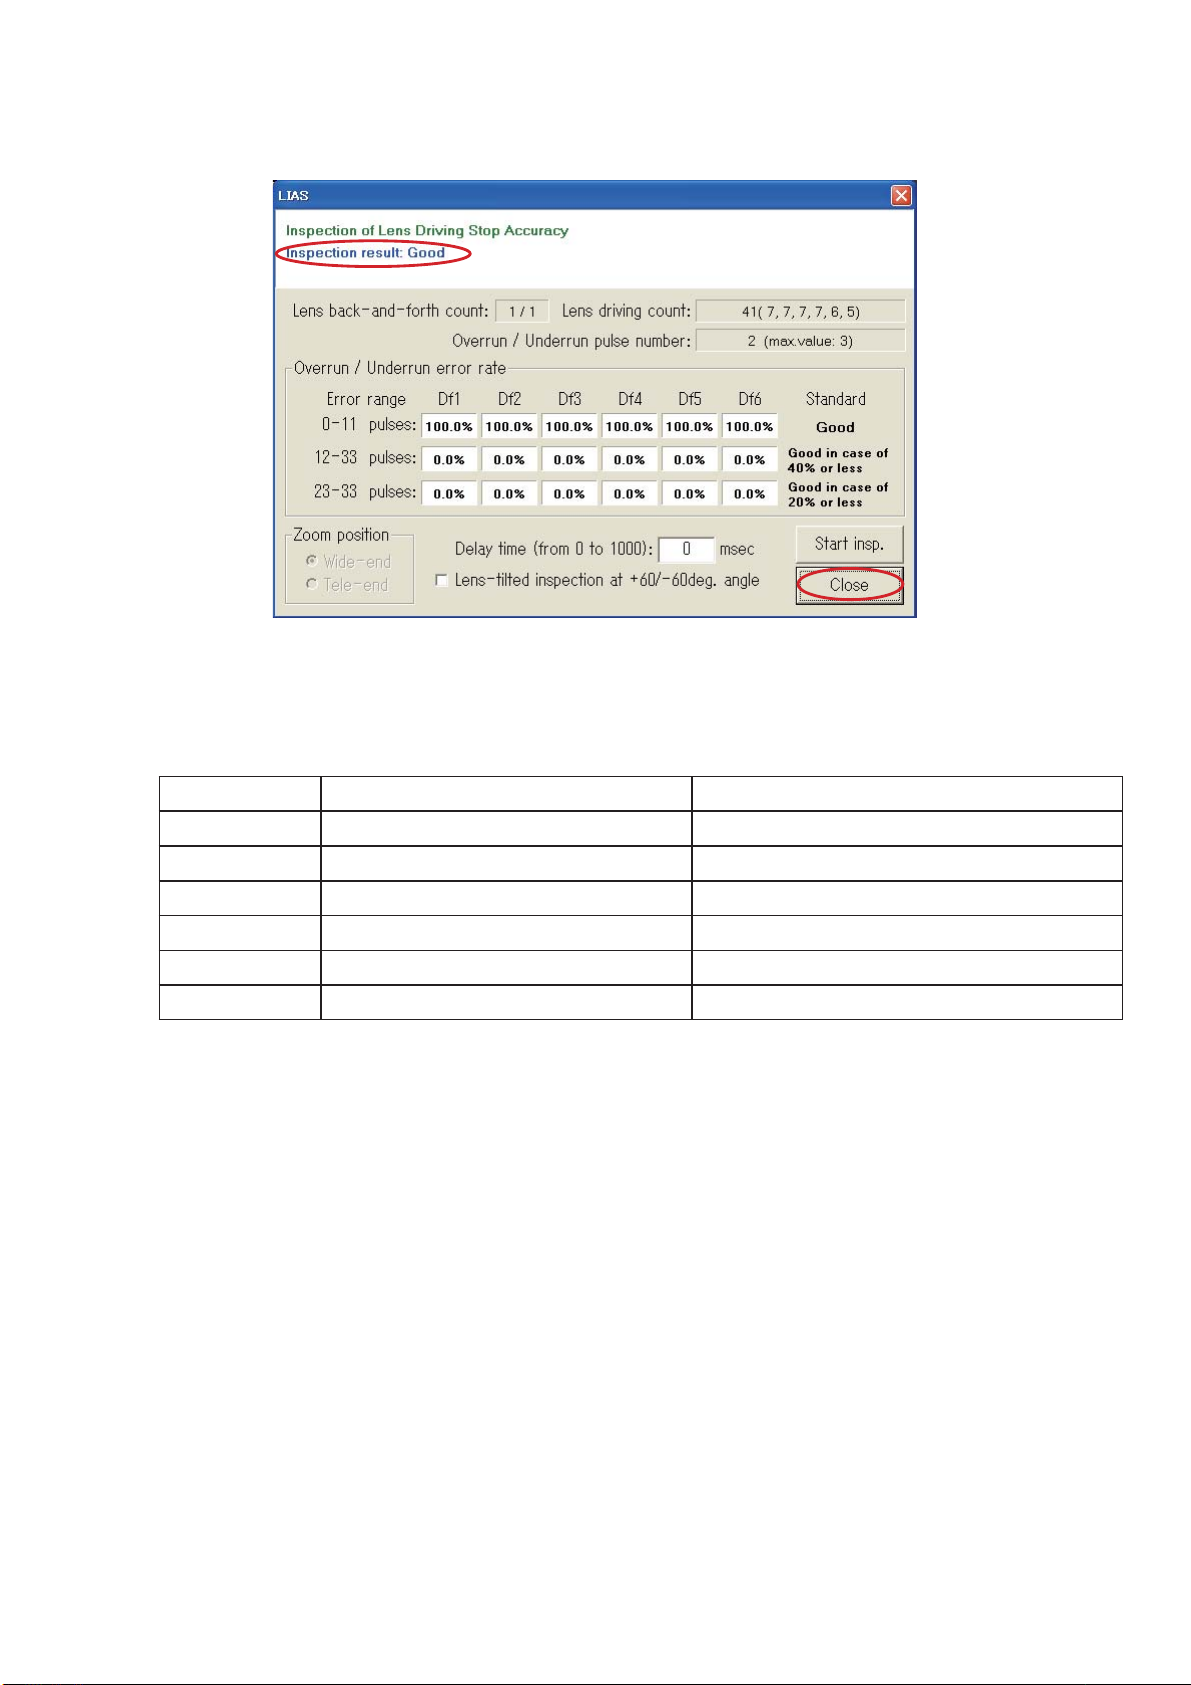
INC
If "Inspection result" shows "Good", click "Close" to end the procedure.
JAA80051-R.3741.A
The number of overrun/underrun pulses must be within the following standards after the lens back-and-forth
driving 1-motion.
Lens position Error range of Df1 - Df6 (No. of occurrence) Error pulse occurrence ratio: Judgment
Horizontal 0~11 GOOD
Horizontal 12~33 GOOD if 40% or less
Horizontal 23~33 GOOD if 20% or less
±60° 0~11 GOOD
±60° 12~33 GOOD if 40% or less
±60° 23~33 GOOD if 20% or less
※
"Df1~Df6" shows the lens driving amount.
- A72・AF-S DX 16-85/3.5-5.6G VR -
Page 95
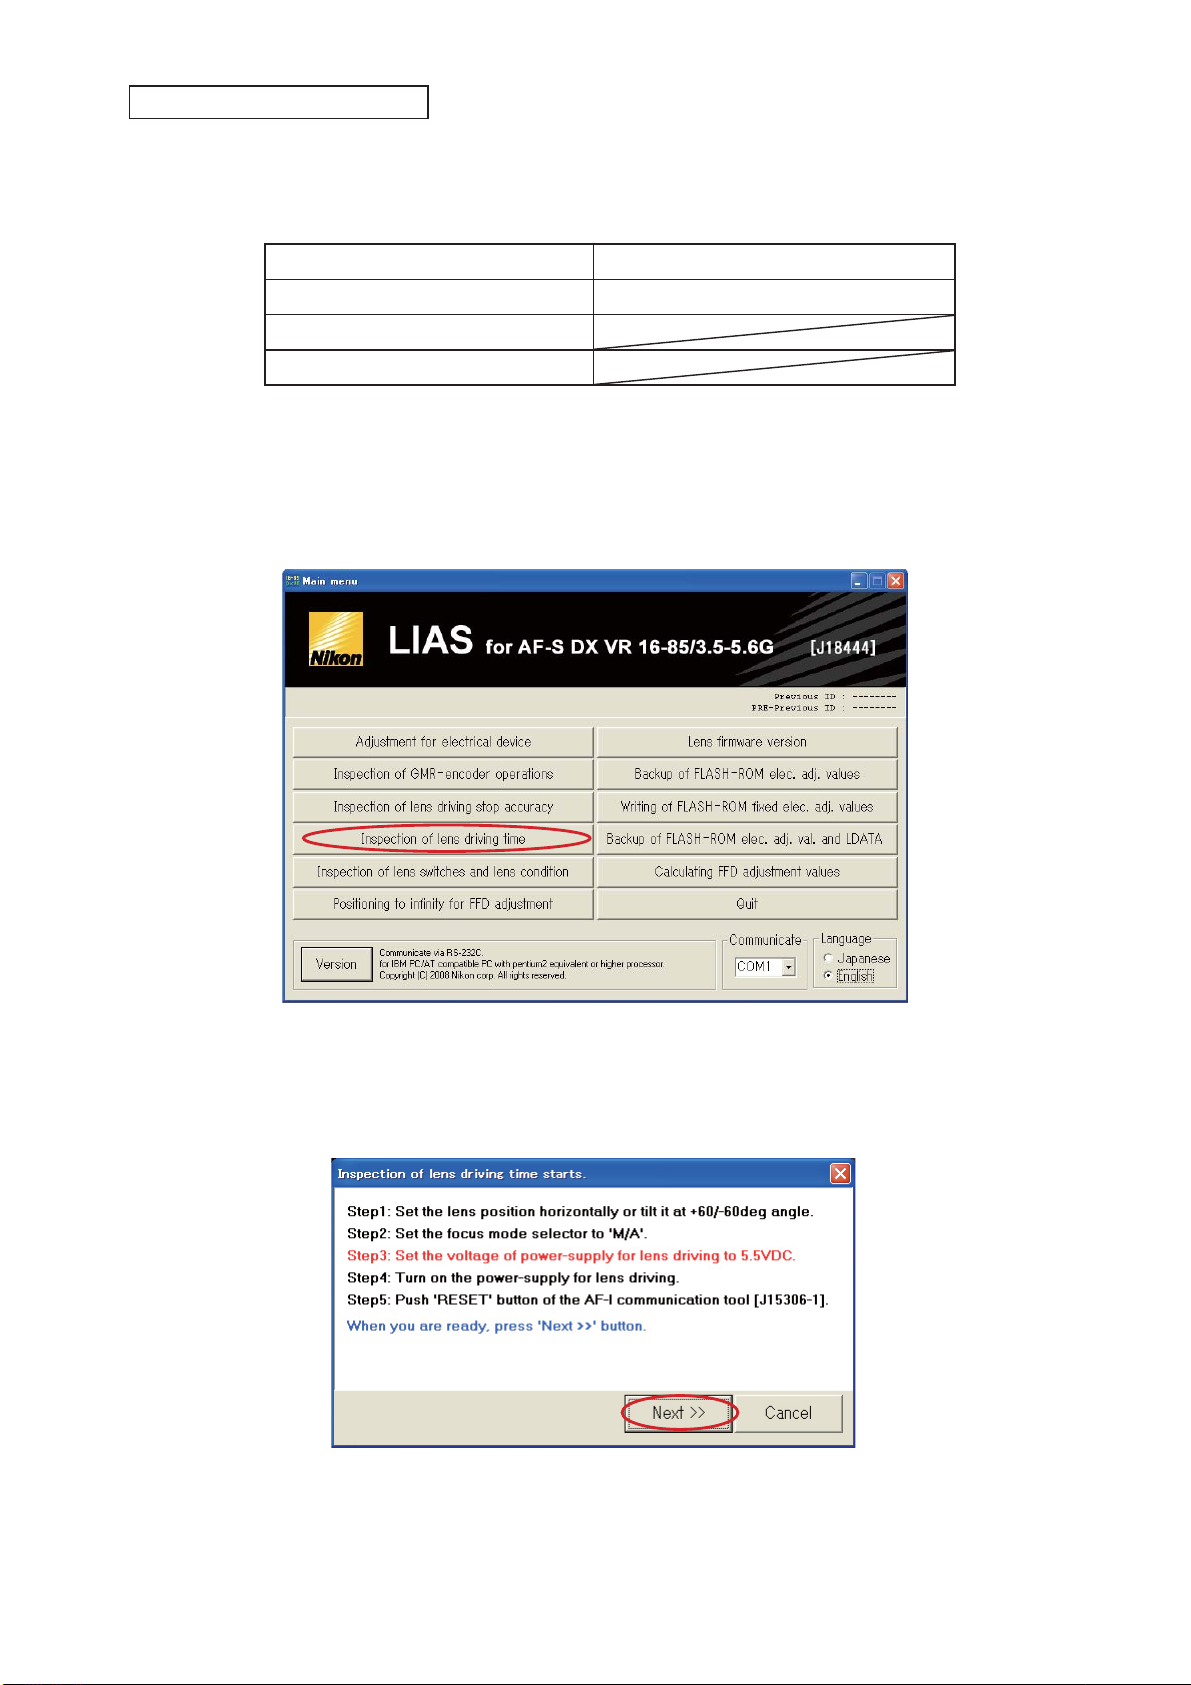
Inspection of lens driving time
INC
●
Make inspections by focal length 16mm (W) or 85m (T) at the following fi ve lens positions.
(Lens position in inspecting)
Lens position Index position
JAA80051-R.3741.A
Horizontal lens position Index facing (1)
(4) Front lens group 60° angle upward
(5) Front lens group 60° angle downward
Click "Inspection of lens driving time" on the main menu.
・
up / (2) right / (3) left
・
Follow the instructions on the screen. When prepared, click "Next".
- A73・AF-S DX 16-85/3.5-5.6G VR -
Page 96
JAA80051-R.3741.A
INC
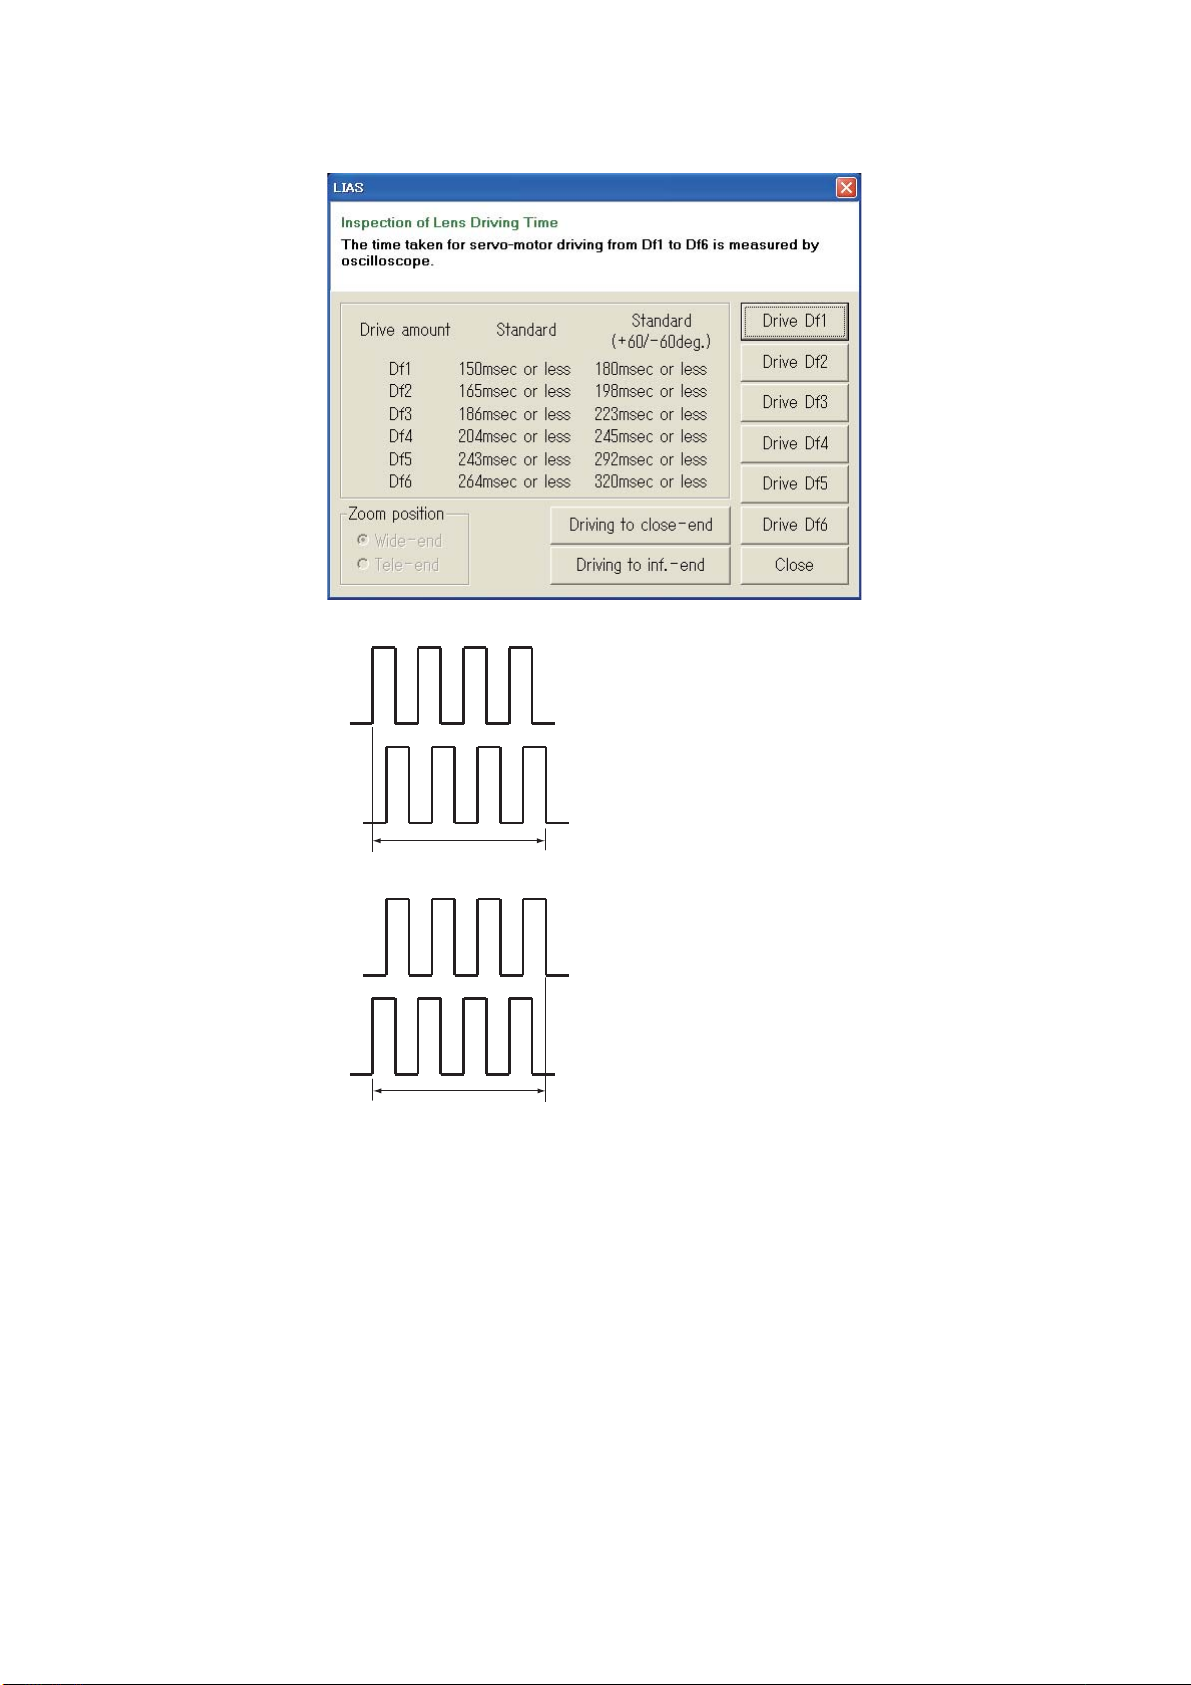
・ Select the driving amount respectively. Each lens driving time must be within the standard.
E terminal
H terminal
E terminal
H terminal
Driving time
Driving time
●Oscilloscope setting
V/Div
Coupling
Time/Div
Trigger Mode
Trigger Coupling
Trigger Source
※ There are two types in shape of waveforms of E and H terminals:
Waveform (1) starts and goes up (2) starts and goes down.
5V
:
DC
:
20m Sec
:
SGL (S)
:
DC
:
CH1
:
- A74・AF-S DX 16-85/3.5-5.6G VR -
Page 97
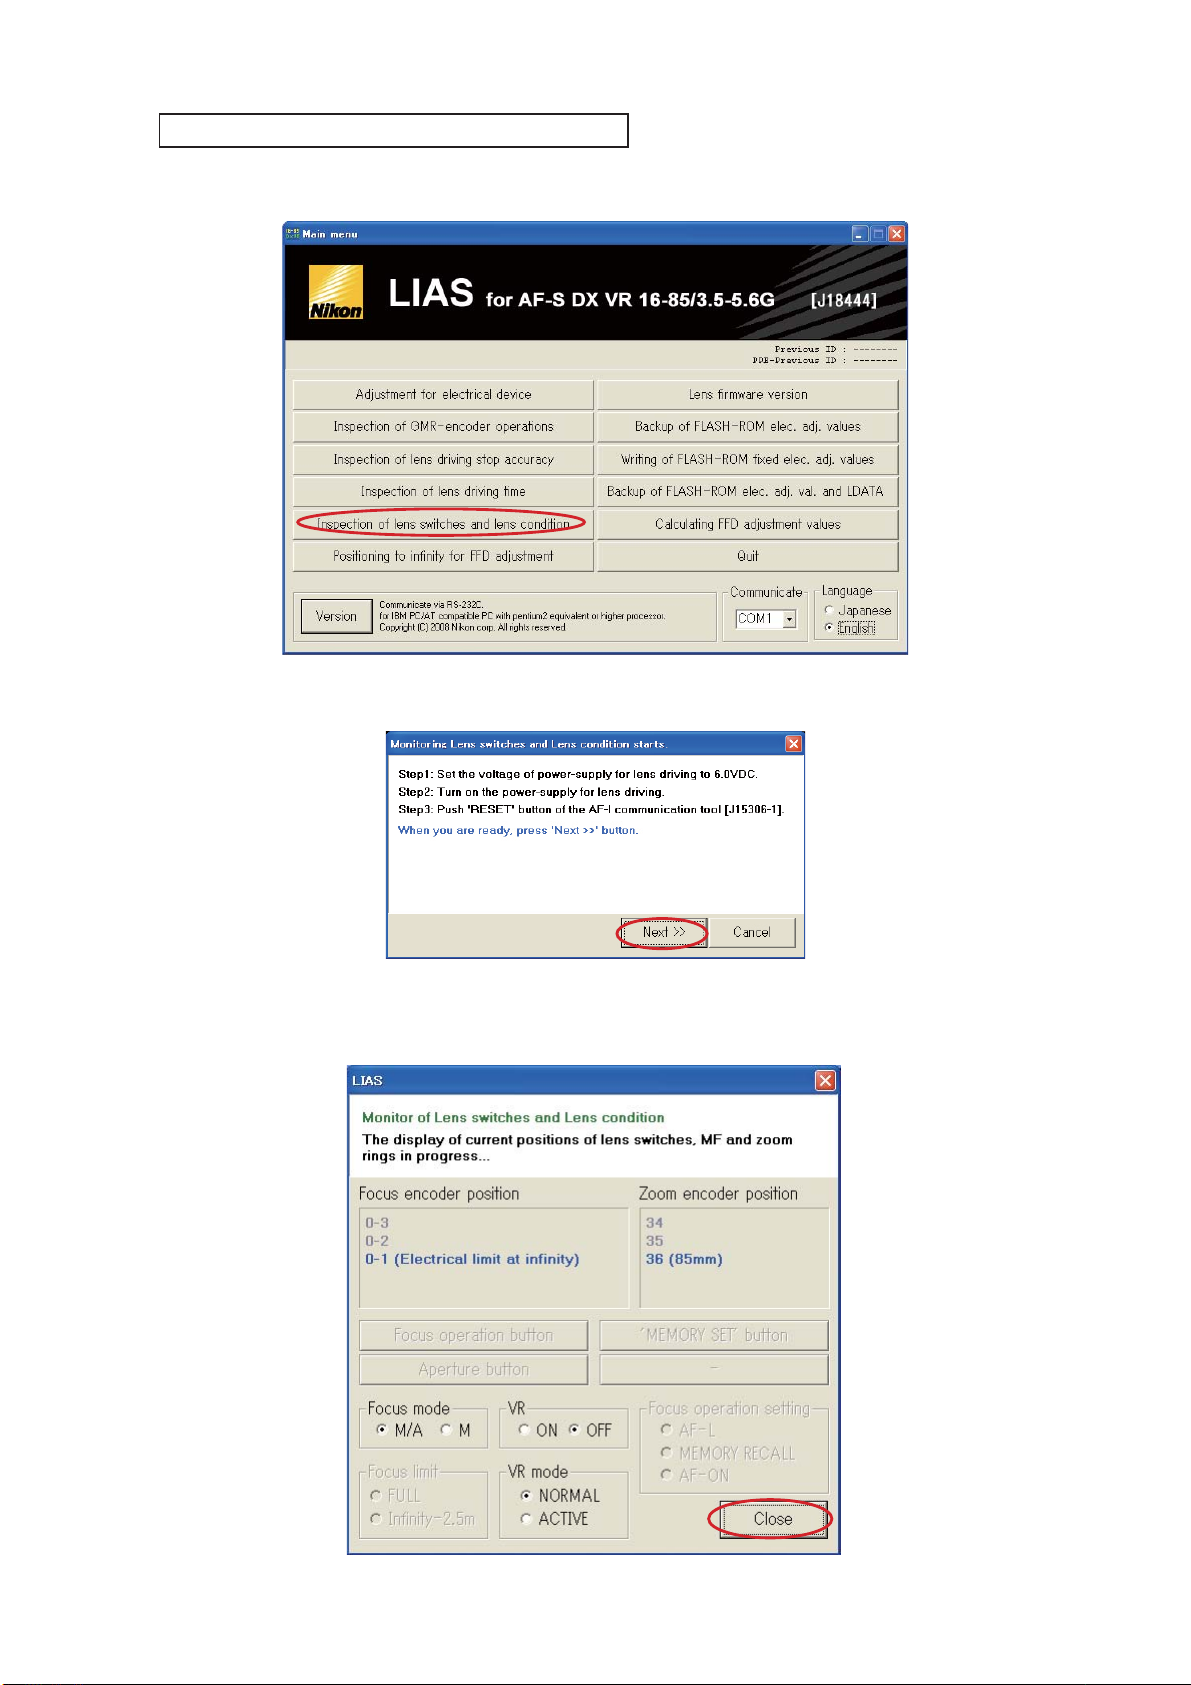
Inspection of Lens switches and Lens conditions
INC
Click "Inspection of lens switches and lens condition" on the main menu.
・
JAA80051-R.3741.A
Follow the instructions on the screen. When prepared, click "Next".
・
If there is no problem with each check item, click "Close" to end the procedure.
・
- A75・AF-S DX 16-85/3.5-5.6G VR -
Page 98
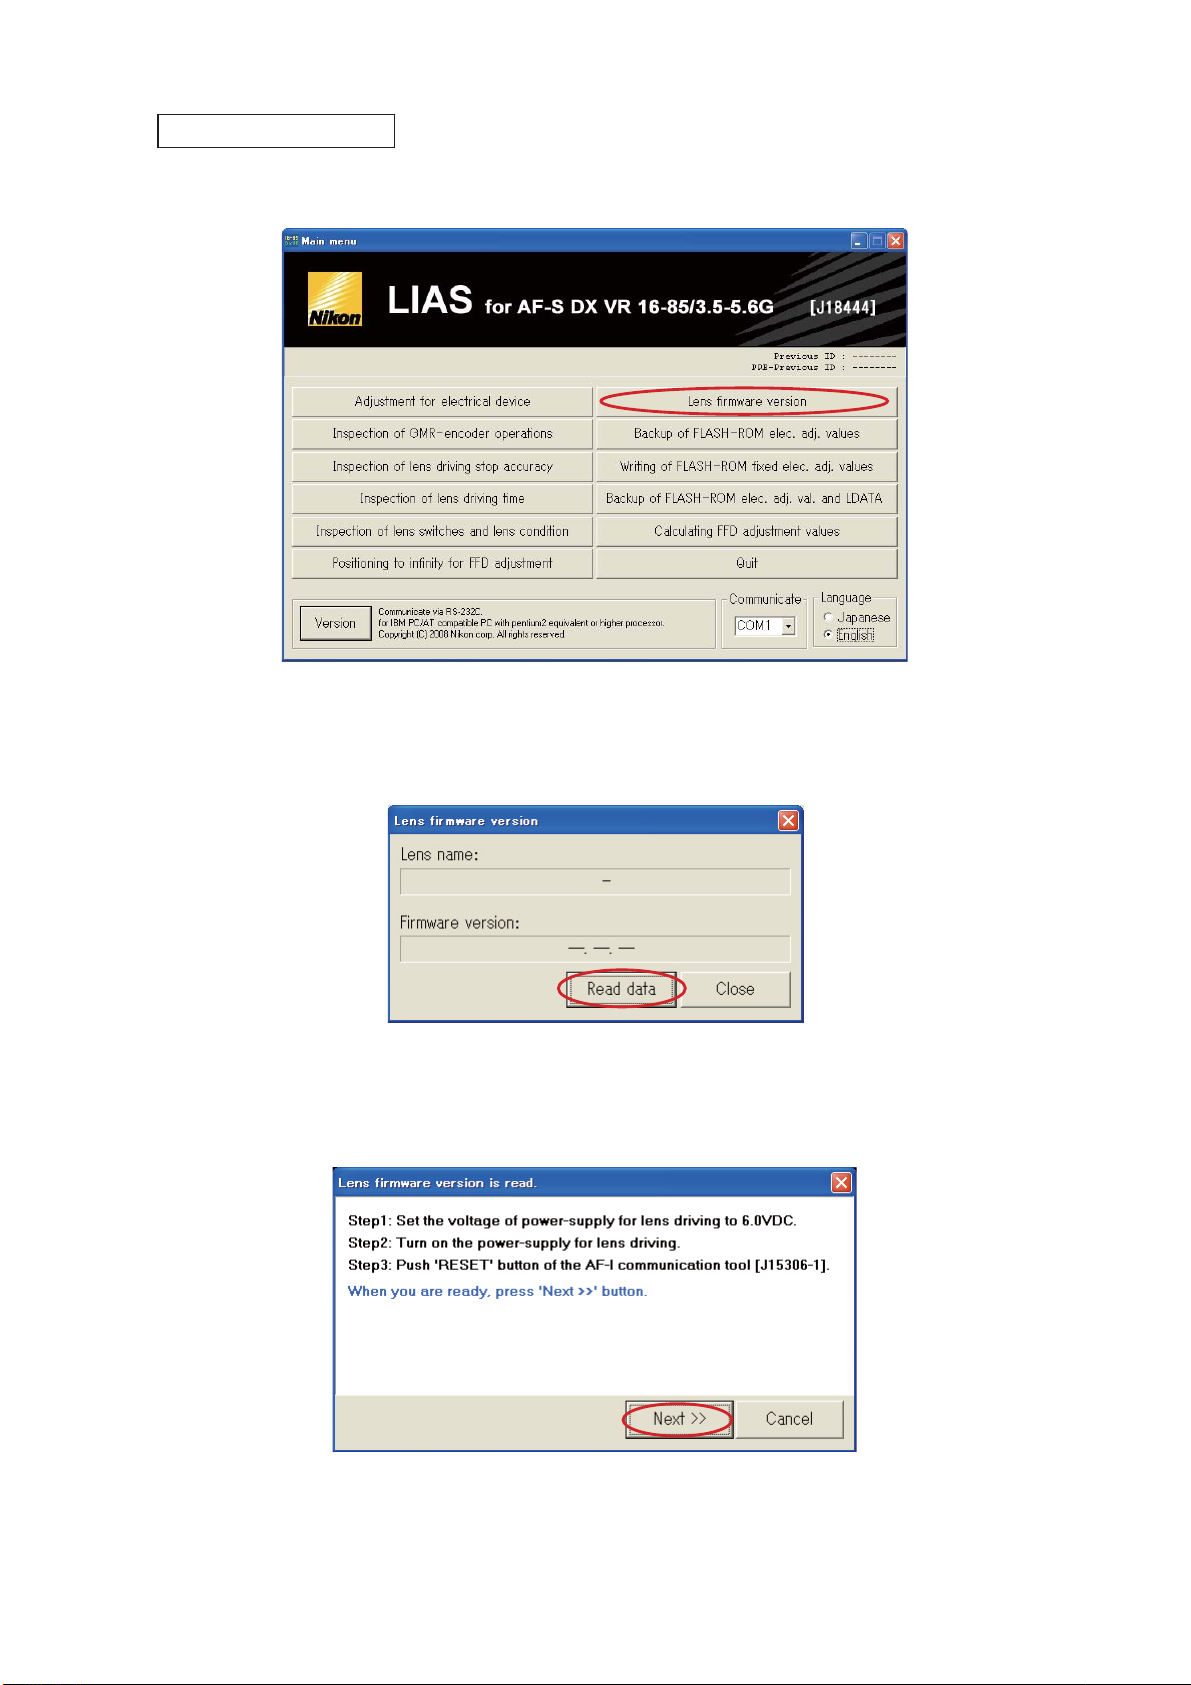
Lens fi rmware version
INC
Click "Lens fi rmware version" on the main menu.
・
JAA80051-R.3741.A
Click "Read data".
・
Follow the instructions on the screen. When prepared, click "Next".
・
- A76・AF-S DX 16-85/3.5-5.6G VR -
Page 99
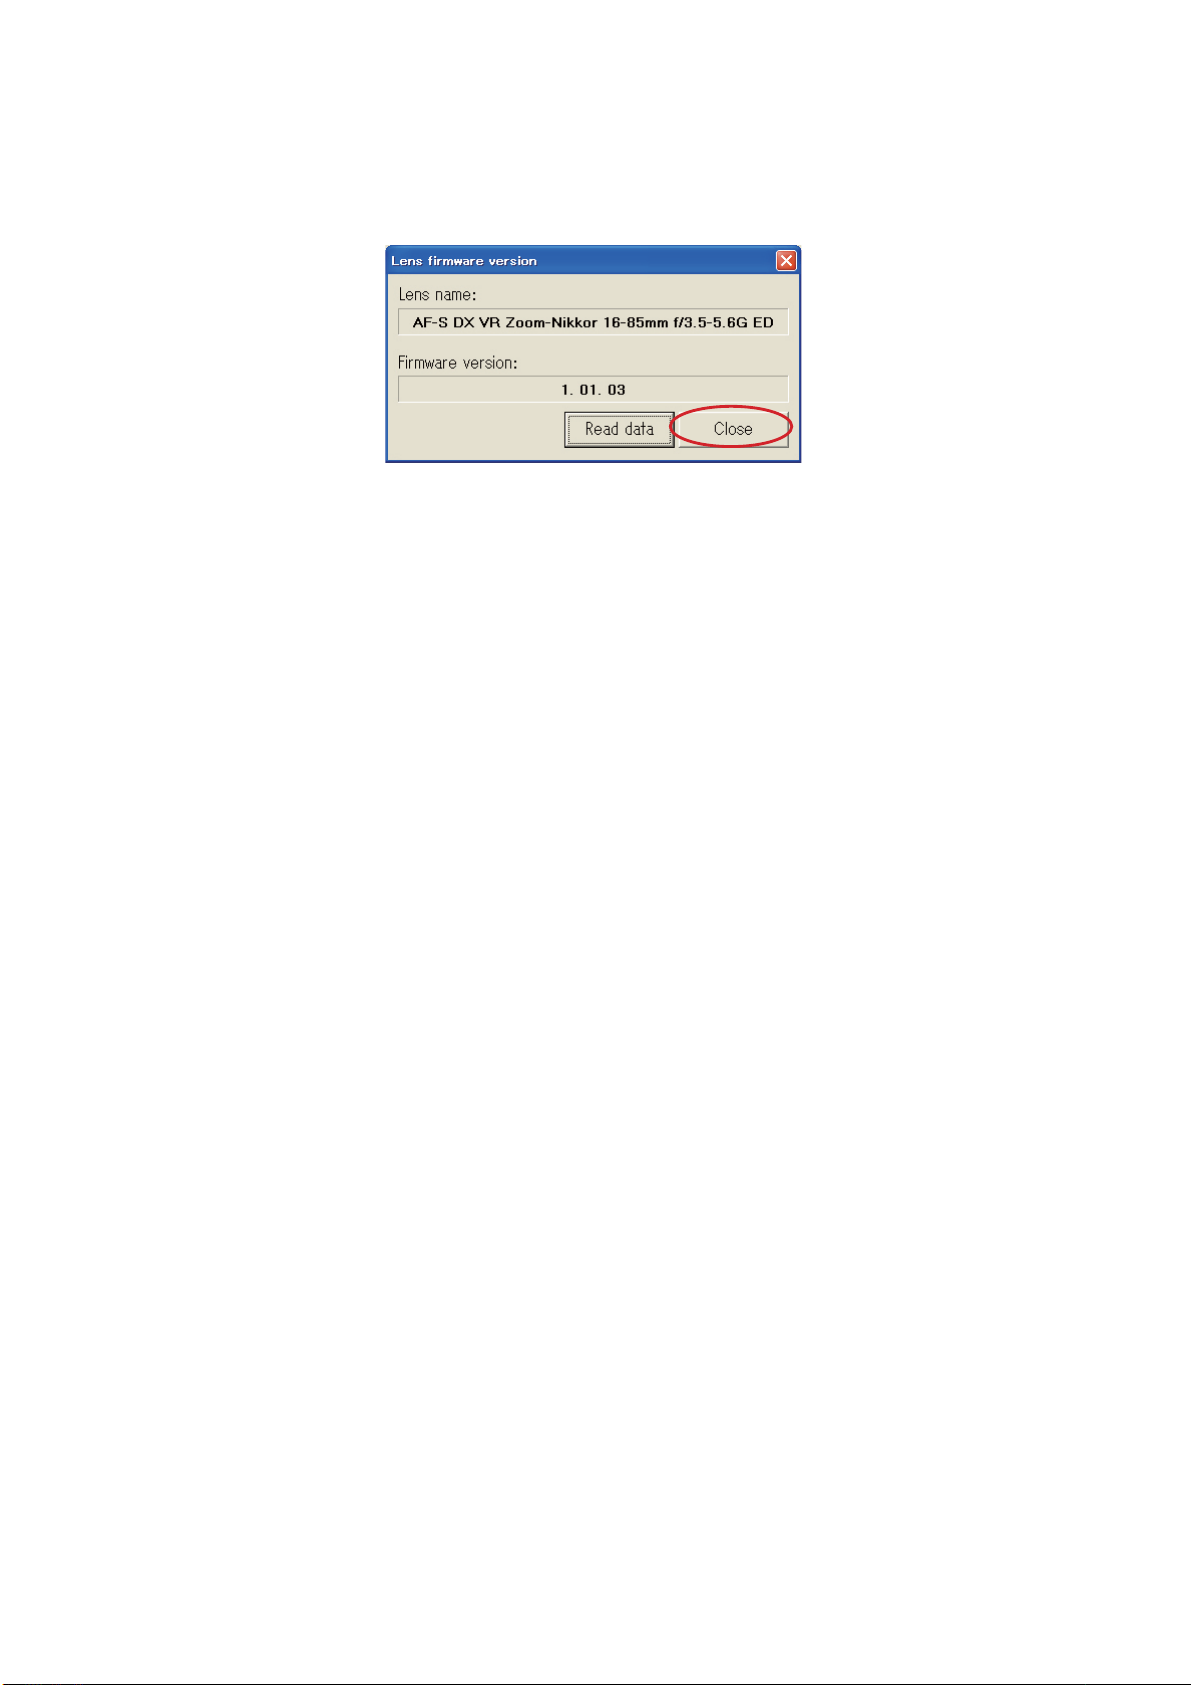
JAA80051-R.3741.A
INC
Confi rm that there is no mistake in the lens name and fi rmware version. Then click "Close" to end the
・
procedure.
- A77・AF-S DX 16-85/3.5-5.6G VR -
Page 100
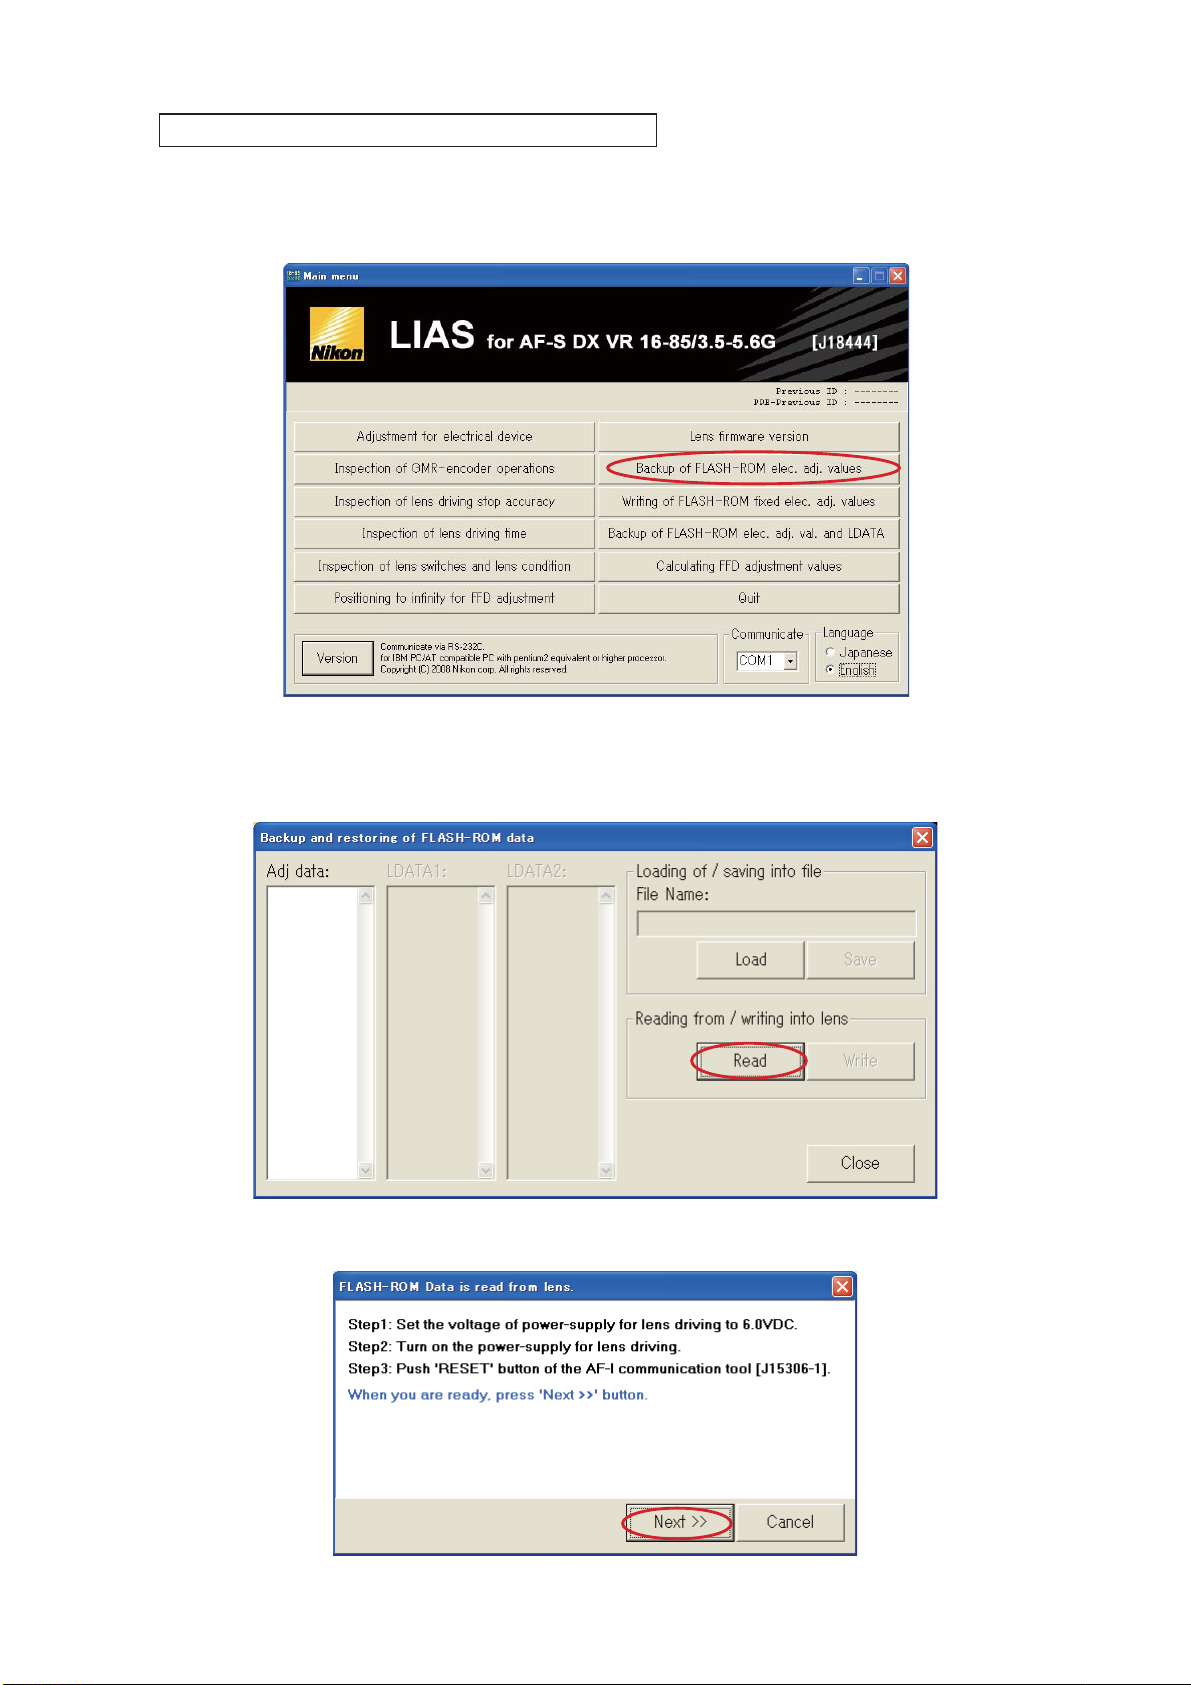
Backup of FLASH-ROM electrical adjustment values
INC
How to back up:
Click "Backup of FLASH-ROM elec. adj. values" on the main menu.
・
JAA80051-R.3741.A
Click "Read" of "Reading from/Writing into lens".
・
・
Follow the instructions on the screen. When prepared, click "Next".
- A78・AF-S DX 16-85/3.5-5.6G VR -
 Loading...