

Page 1
Model
1098 Press
INSTRUCTION MANUAL
Sonics & Materials, Inc.
Page 2
W A R N I N G
Go To Top Of Document
SAFETY PRECAUTIONS
READ BEFORE INSTALLING OR USING THE EQUIPMENT
Our systems have been designed to assure maximum operator safety.
However, no design can completely protect against improper usage. For
maximum safety and equipment protection, observe the following warnings at
all times and read all applicable instruction manuals carefully before you
attempt to operate any equipment.
– The equipment has safety devices that require both hands to be on the
palm buttons until the horn contacts the work piece. Do not defeat or
modify these safety devices.
– Do not use with foot switch unless alternate means of pinch-point
protection is provided.
– High voltage is present in the equipment. Disconnect plug before removing
cover or servicing.
– Make sure equipment is properly grounded with a 3-prong plug. Before
plugging in equipment, test outlet for proper earth grounding.
– High voltage potential may be present in the converter as a result of
temperature changes. Do not touch the converter contact unless you first
short both pins or the button to the converter case with an insulated tool.
– Never squeeze or grab a vibrating horn.
– Do not modify horn configurations.
– Ultrasonic welders operate above normal audibility for most people. Ear
protection is recommended. Consult the Appendix for a list of
manufacturers of ear protectors.
– Do not affix any device to any portion of the horn.
Sonics & Materials, Inc.
Corporate Headquarters European Office
53 Church Hill Road • Newtown, CT 06470 USA 22 ch du Vernay • CH - 1196 Gland, Switzerland
203.270.4600 • 800.745.1105 • 203.270.4610 fax (41) (0) 22/364 1520 • (41) (0) 22/364 2161 fax
Information contained in this manual is subject to change without notice. Sonics & Materials, Inc. is not responsible for any typographic errors.
© Sonics & Materials, Inc. 2007 Printed in U.S.A. Part No. 381-0037
Rev 5/07
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I NS T R U C T I O N M A N U A L • MO D E L 10 9 8
1
Page 3
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
Go To Top Of Document
2
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 4
T A B L E O F C O N T E N T S
Go To Top Of Document
IMPORTANT SERVICE LITERATURE . . . . . . . . . . . . . . . . . . . . . . . . . . . .4
Manual Change Information . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .4
UNPACKING AND INSPECTION . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .5
Visible Loss or Damage . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .5
Concealed Loss or Damage . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .5
INTRODUCTION . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .6
OVERVIEW OF ULTRASONIC PLASTICS ASSEMBLY . . . . . . . . . . . . . .6
What is Ultrasonics? . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .6
Principal of Ultrasonic Assembly . . . . . . . . . . . . . . . . . . . . . . . . . . .6
Ultrasonic Assembly Systems . . . . . . . . . . . . . . . . . . . . . . . . . . . . .6
GLOSSARY OF ULTRASONIC TERMS . . . . . . . . . . . . . . . . . . . . . . . . . . .8
INSTALLATION . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .9
Electrical Power . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .9
Air Supply . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .9
Setting Up . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .9
Connections . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .10
Options . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .10
OPERATING PROCEDURES . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .11
Control Panel . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .11
INITIAL EQUIPMENT SETUP . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .12
Assembling and Mounting Converter, Booster and Horn . . . . . . .12
Horn and Fixture Alignment . . . . . . . . . . . . . . . . . . . . . . . . . . . . .14
Positive Stop Adjustment . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .15
OPERATION . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .16
Actuation . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .16
Emergency Stop . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .16
FINE ADJUSTMENTS . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .17
Pressure Switch Adjustment . . . . . . . . . . . . . . . . . . . . . . . . . . . . .17
Booster Selection . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .18
Pressure . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .18
Stroke Speed Adjustment . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .19
Re-Establishing Proper Booster/Horn Interfaces . . . . . . . . . . . . .20
MAINTENANCE . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .21
Repairs / Service . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .21
WARRANTY . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .22
Limitation of Warranty . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .22
APPENDIX . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . .24
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
3
Page 5
I M P O R T A N T S E R V I C E L I T E R A T U R E
Go To Top Of Document
The system supplied with this instruction manual is constructed of the finest
material and the workmanship meets the highest manufacturing standards. It
has been thoroughly tested and inspected before leaving the factory and
when used in accordance with the procedures outlined in this manual, will
provide you with many years of safe and dependable service.
NOTE: Please read
carefully before operating
the equipment, then
forward to your service
department.
MANUAL CHANGE INFORMATION
We continually strive to be at the forefront of the latest electronic
developments by adding circuit and component improvements to our
equipment as soon as they are developed and tested.
Sometimes, due to printing and shipping requirements, we cannot incorporate
these changes immediately into printed manuals. Hence, your manual may
contain new change information. Change information, if any, is located in the
Appendix.
We reserve the right to make any changes in the design or construction of our
equipment at any time, without incurring any obligation to make any change
whatsoever in units previously delivered.
The technical data and schematics in the manual are for informational
purposes only and may not reflect the current configuration being shipped
from our factory. Upon formal request, complete and up-to-date information
can be provided from the factory free of charge.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
4
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 6
U N P A C K I N G A N D I N S P E C T I O N
Go To Top Of Document
Before unpacking the equipment, check the shipping carton for any visible
damage. If you see any, be sure to follow the procedures described below
under “Visible Loss or Damage.” Otherwise, proceed to remove the equipment
from the carton. Before disposing of any packing material, check it carefully
for small parts. Then perform a visual inspection of the equipment to detect
NOTE: We recommend
keeping all carton(s) and
packing material in case it
might be necessary to
move the equipment, or to
ship it for repair.
any evidence of damage which might have occurred during shipment. Check
the following:
1. all components against the enclosed packing list,
2. all module plug-in units,
3. all wire plug-in connections.
The equipment was carefully packed and thoroughly inspected before leaving
our factory. All units are tested and checked for problems prior to shipping. It
is asked that when a problem does occur that all parts and components be
inspected for damage (especially when the unit is not in working order when
received). Responsibility for safe delivery was assumed by the carrier upon
acceptance of the shipment. Claims for loss of damage sustained in transit
must therefore be made upon the carrier, as follows:
VISIBLE LOSS OR DAMAGE
Any external evidence of loss or damage must be noted on the freight bill or
express receipt, and signed by the carrier’s agent. Failure to adequately
describe such external evidence of loss or damage may result in the carrier’s
refusal to honor a damage claim. The form required to file such a claim will
be supplied by the carrier.
CONCEALED LOSS OR DAMAGE
Concealed loss or damage means loss or damage which does not become
apparent until the merchandise has been unpacked. The contents might have
been damaged in transit due to rough handling even though the container
may not show external damage. When the damage is discovered upon
unpacking, make a written request for inspection by the carrier’s agent within
48 hours of the delivery date. Then file a claim with the carrier since such
damage is the carrier’s responsibility. The form required to file such a claim
will be supplied by the carrier. Do not destroy packing materials, or move
material from one location to another before the carrier makes their
inspection.
If the system or any unit is damaged, notify “Sonics.” “Sonics” will arrange for
repair or replacement of damaged equipment without waiting for the claim
against the carrier to be settled, provided a new purchase order is issued to
cover the repair or replacement costs. Should any damage, shortage or
discrepancy exist, please notify us immediately.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
5
Page 7
I N T R O D U C T I O N
Go To Top Of Document
The model 1098 press is a 20 kHz precision pneumatic actuator (tabletop
version) used for ultrasonic plastics assembly. The 1098 press can be
supplied with the following power supplies:
■ FD . . . . . . . . . . . . . .Timer
■ FDL . . . . . . . . . . . . .Timer/Linear Encoder
■ FM . . . . . . . . . . . . . .Microsonic Processor™
■ FO/ML . . . . . . . . . . .Microsonic Processor™/Linear Encoder
O V E R V I E W O F U L T R A S O N I C P L A S T I C S A S S E M B L Y
WHAT IS ULTRASONICS?
Ultrasonics refers to vibrational waves with a frequency above the human
audible range which is usually above 18,000 cycles per second (Hz).
PRINCIPLE OF ULTRASONIC ASSEMBLY
The basic principle of ultrasonic assembly involves conversion of high
frequency electrical energy to high frequency mechanical energy in the form
of reciprocating vertical motion which, when applied to a thermoplastic,
generates frictional heat at the plastic/plastic or plastic/metal interface. In
ultrasonic welding, this frictional heat melts the plastic, allowing the two
surfaces to fuse together; in ultrasonic staking or insertion, the controlled flow
of molten plastic is used to capture or lock another material in place (staking)
or encapsulate a metal insert (insertion).
ULTRASONIC ASSEMBLY SYSTEMS
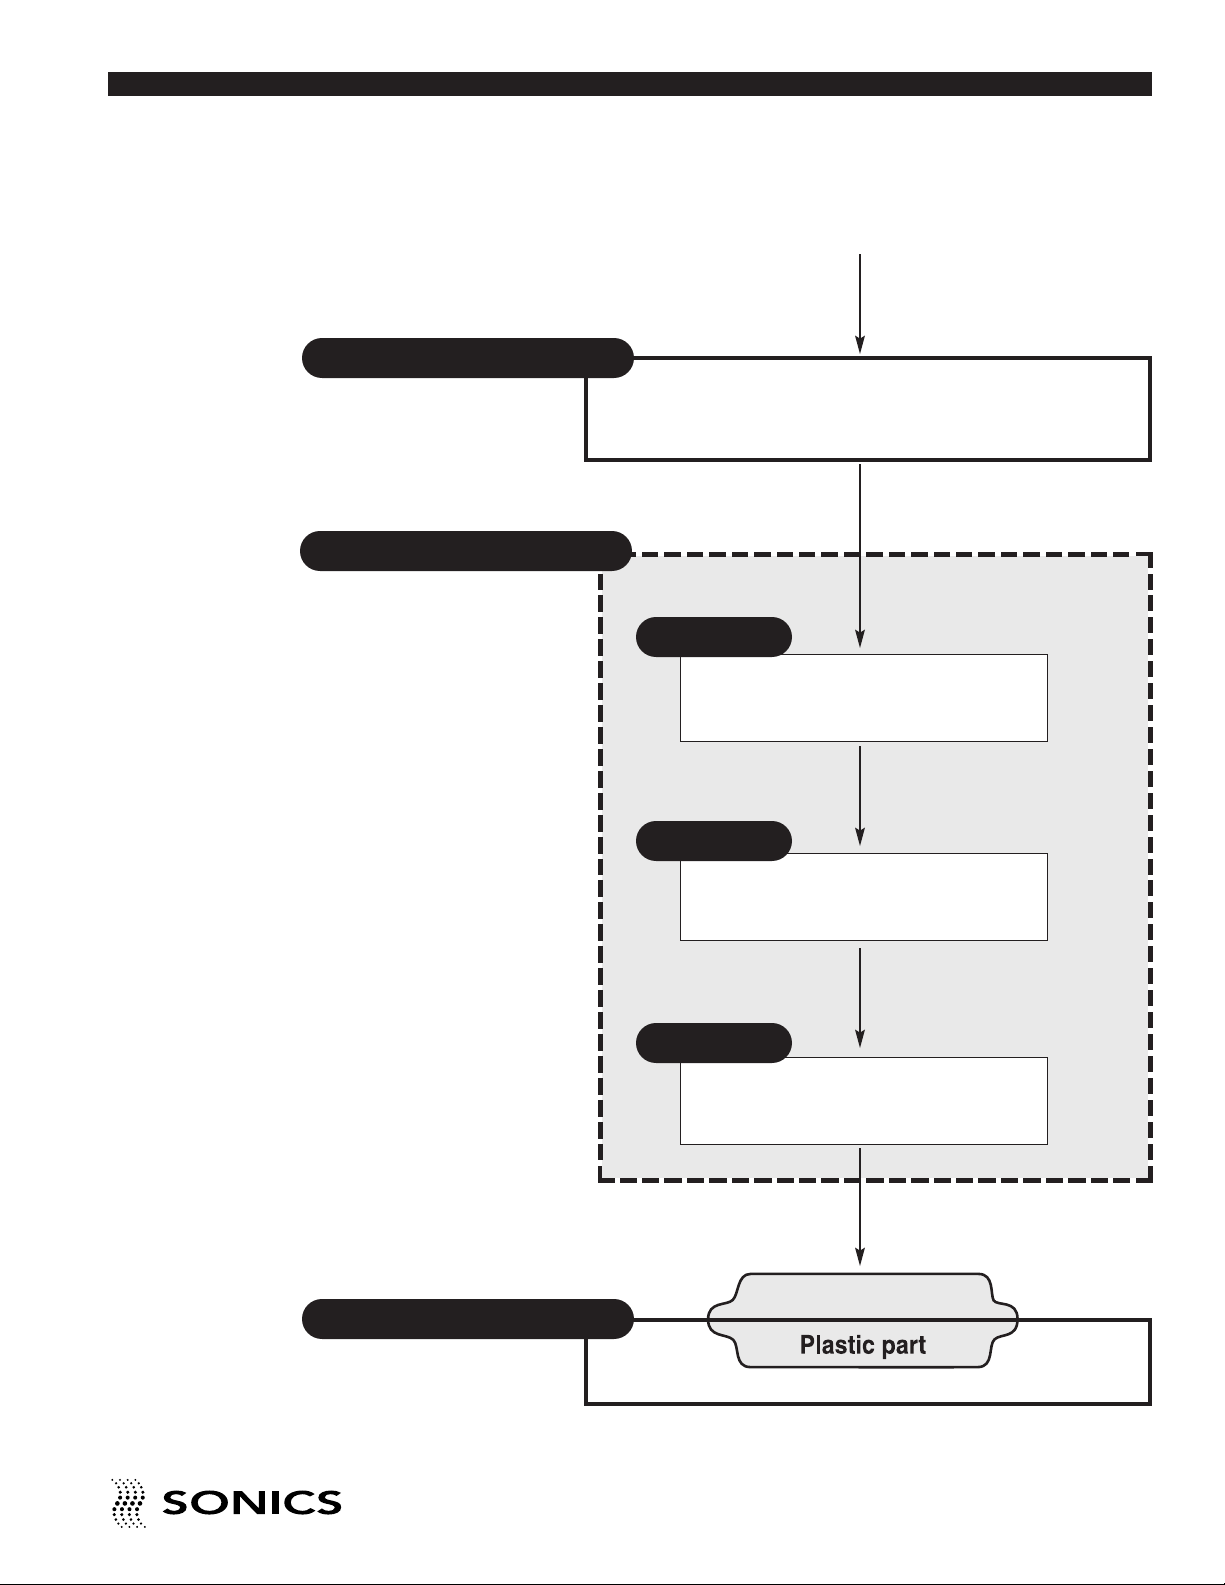
“Sonics” ultrasonic assembly systems are generally composed of the
following major elements: a power supply, converter, booster, horn, pneumatic
press and holding fixture, as detailed in the diagram on the next page. A
review of this diagram will help you understand the basic elements involved in
the assembly process and their relation to each other.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
6
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 8
“SONICS” ULTRASONIC ASSEMBLY SYSTEMS
Go To Top Of Document
Power Supply/Generator
Actuator/Press
Provides compressive force
and mounting for Converter,
Booster, Horn assembly
50/60 Hz
Electrical power
Generates ultrasonic electrical energy
(15/20/40 kHz)
Ultrasonic
electrical energy
Converter
Transforms ultrasonic electrical energy
to ultrasonic mechanical vibrations
Ultrasonic Vibrations
Holding Fixture
Aligns and supports part
Booster
Increases or decreases amplitude
Ultrasonic Vibrations
Horn
Contacts and transfers vibrational
energy to plastic part
Ultrasonic Vibrations
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
7
Page 9
G L O S S A R Y O F U L T R A S O N I C T E R M S
Go To Top Of Document
POWER SUPPLY/GENERATOR – The solid state power supply converts
standard 50/60 Hz electrical power to 15,000 Hz, 20,000 Hz, and 40,000 Hz
(15/20/40 kHz) electrical energy.
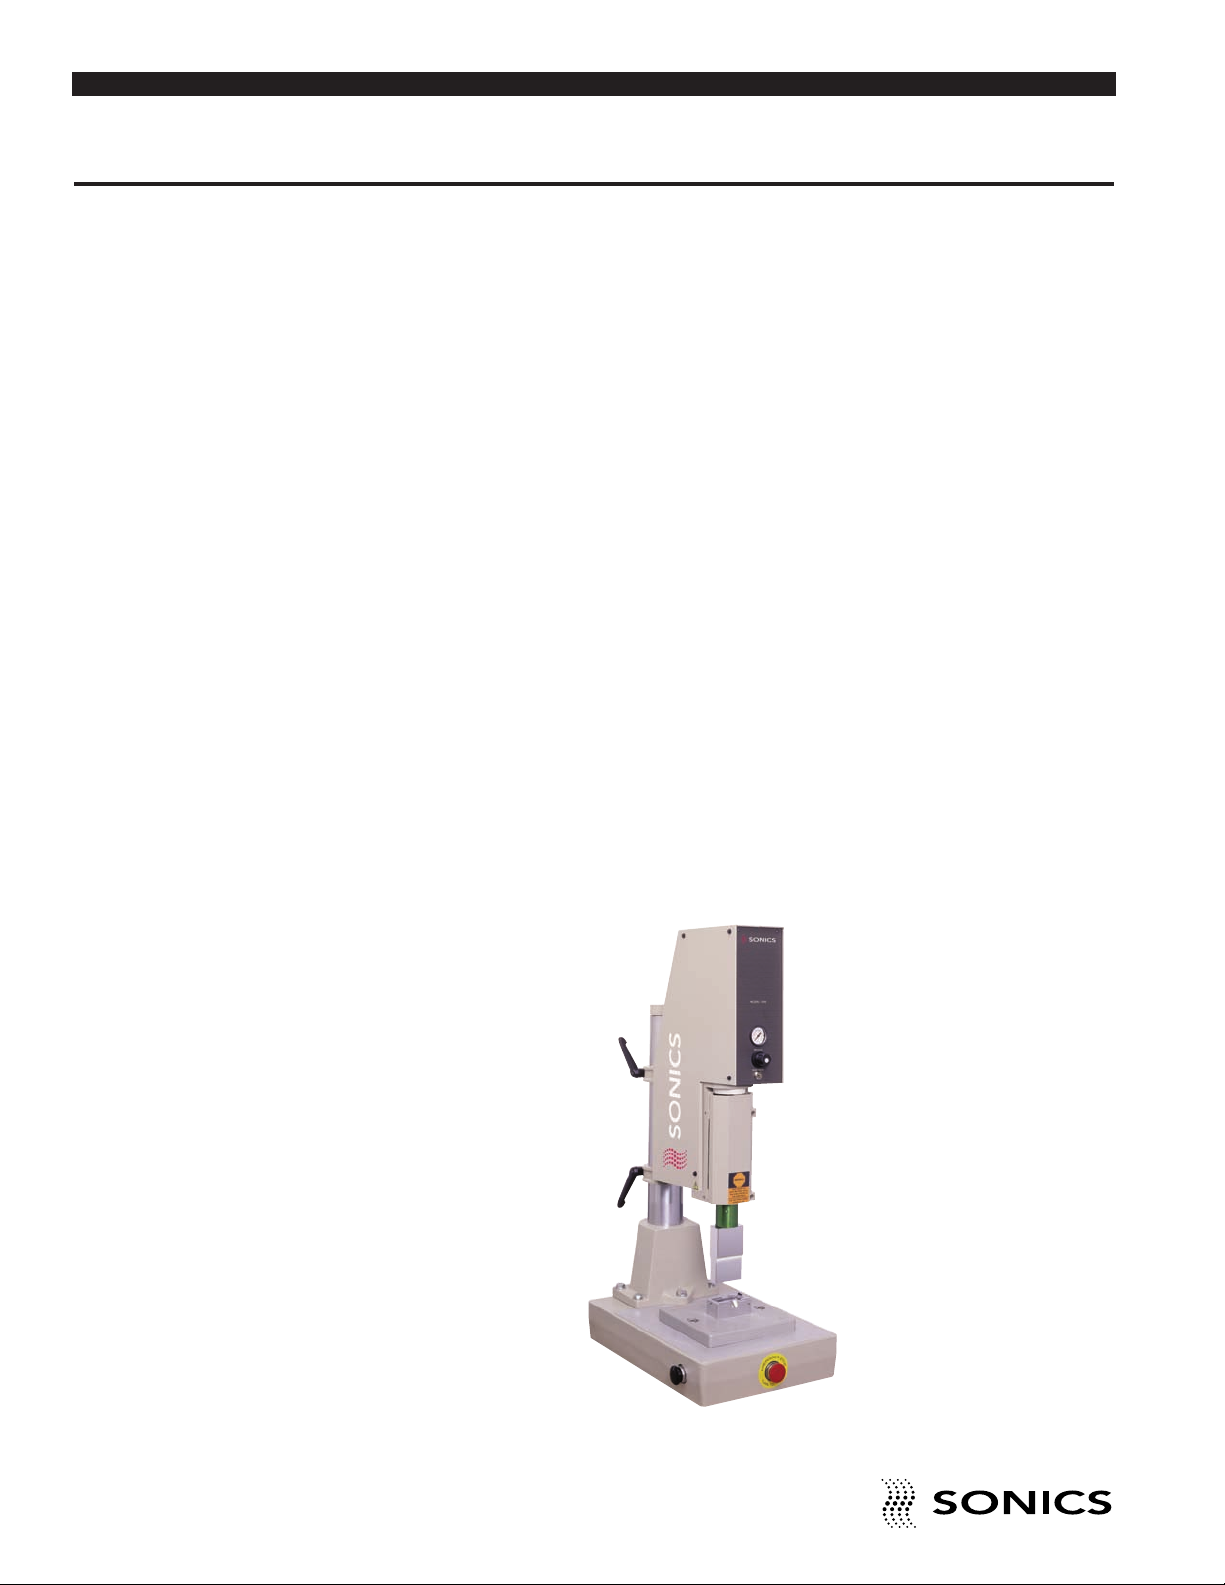
ACTUATOR/PRESS – The pneumatic actuator provides compressive force
and mounting for the converter, booster, and horn assembly. The tabletop
press consists of a base assembly, column and actuator (head).
CONVERTER – The converter changes the high frequency electrical energy
supplied by the power supply to high frequency mechanical vibrations.
BOOSTER – Successful ultrasonic welding often depends on having the right
amplitude at the horn face. Often it is not possible to design a horn which has
both the necessary shape and required gain (ratios of input amplitude to
output amplitude). In such cases, a booster is placed between the converter
and the horn to either increase or decrease the amplitude of the horn. In
addition to changing/maintaining the amplitude, the booster provides support
and alignment in the welding system. (See page 18 for booster selection.)
HORN – The horn is a tuned component of the system which comes in
contact with the parts to be assembled. The horn 1) transfers the ultrasonic
vibrations produced from the converter to the parts being welded, and 2)
applies necessary force to the assembly while the material resolidifies.
HOLDING FIXTURE – The holding fixture or nest assures proper alignment
and support of the parts being assembled.
MODEL 1098
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
8
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 10
I N S T A L L A T I O N
Go To Top Of Document
ELECTRICAL POWER
The press is powered by the power supply. Consult your power supply
instruction manual to determine power specifications.
AIR SUPPLY
The press requires a source of dry, filtered (5 micron), oil-free, compressed
air capable of supplying a constant line pressure of 85 psig. (586 kPa / 6 bar)
at a minimum capacity of 2 CFM.
Do not connect the press
to an air source supplied
by a compressor lubricated
with synthetic oils or oils
containing phosphate
esters or chlorinated hydrocarbons. This type of
lubricant may cause the air
filter to malfunction, and
the plastic bowl to rupture.
NOTE: If the power supply
is to be run continuously,
air cooling of the converter
and horn is required. Use
clean, dry compressed air
filtered down to 5 microns
(supplied to converter
fitting).
SETTING UP
The press should be installed in a clear, uncluttered location that is free from
excessive dirt, dust, corrosive fumes, and temperature and humidity
extremes. The selected installation site should be near the electrical power
and air supply sources and away from any equipment that generates
abnormally high electrical transients. Observe the following additional
instructions when installing the press:
a. The press should be placed on a sturdy, level table or bench capable of
supporting a minimum of 500 pounds (227 kg).
b. Allow at least 6 inches (152.4mm) at the rear of the press for cable
connections.
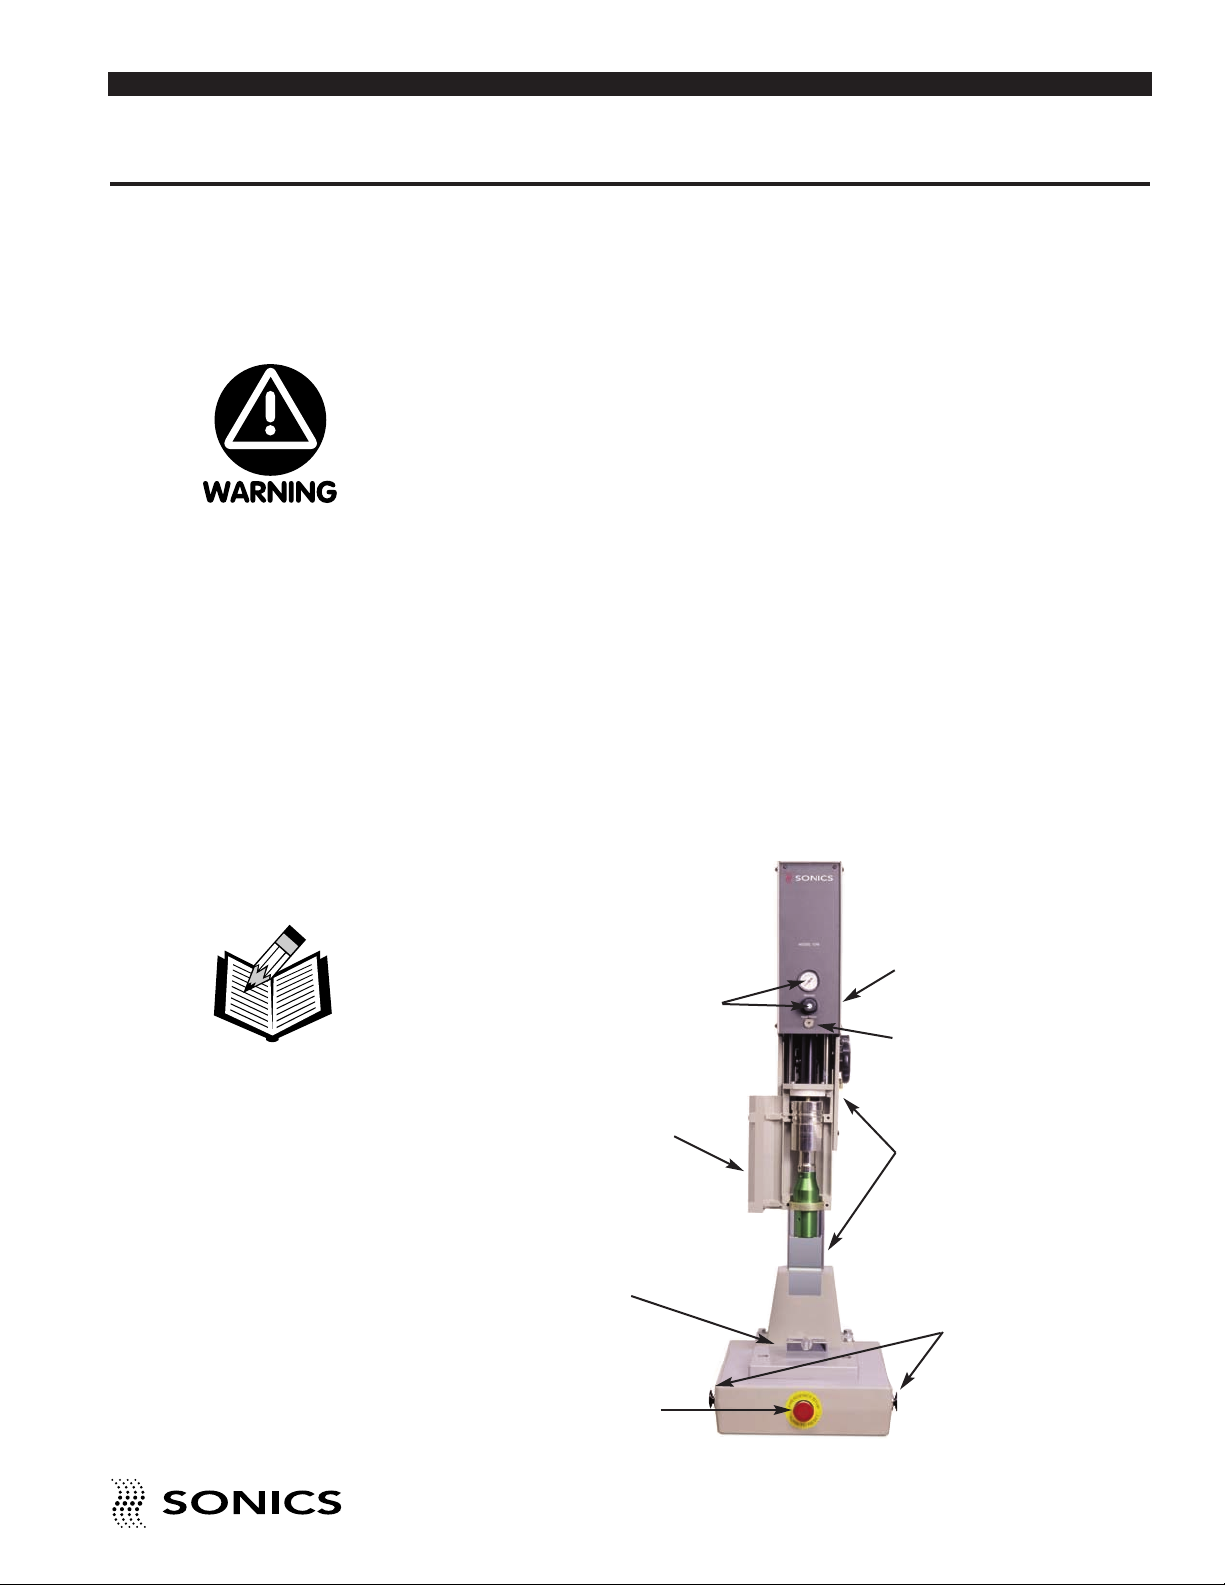
KEY COMPONENTS
PRESSURE
REGULATOR
& GAUGE
CONVERTER
HOUSING DOOR
PART HOLDING
FIXTURE
AIR FILTER
(in rear of press)
HEAD DOWN
KEY SWITCH
CONVERTER HOUSING
with converter, booster &
horn (stack) assembly
PALM BUTTONS
EMERGENCY STOP
BUTTON
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
9
Page 11
NOTE: Do not strain or
Go To Top Of Document
kink the cables. When
going around corners,
allow as wide a bend as
possible. Do not run the
cables parallel to any
power line within a distance
of less than 1 foot
(304.8mm).
CONNECTIONS
When making the initial connections, make sure all power is disconnected.
1. Connect the air supply source to the press air filter located at the right, rear
of the press head, using a hose having a minimum inside diameter of 1/8
inch (3 mm).
2. Connect the RF and base (actuating) cables of the press to the power
supply. (Consult your power supply instruction manual for details.)
3. Check with your electrician if you have any wiring questions.
OPTIONS
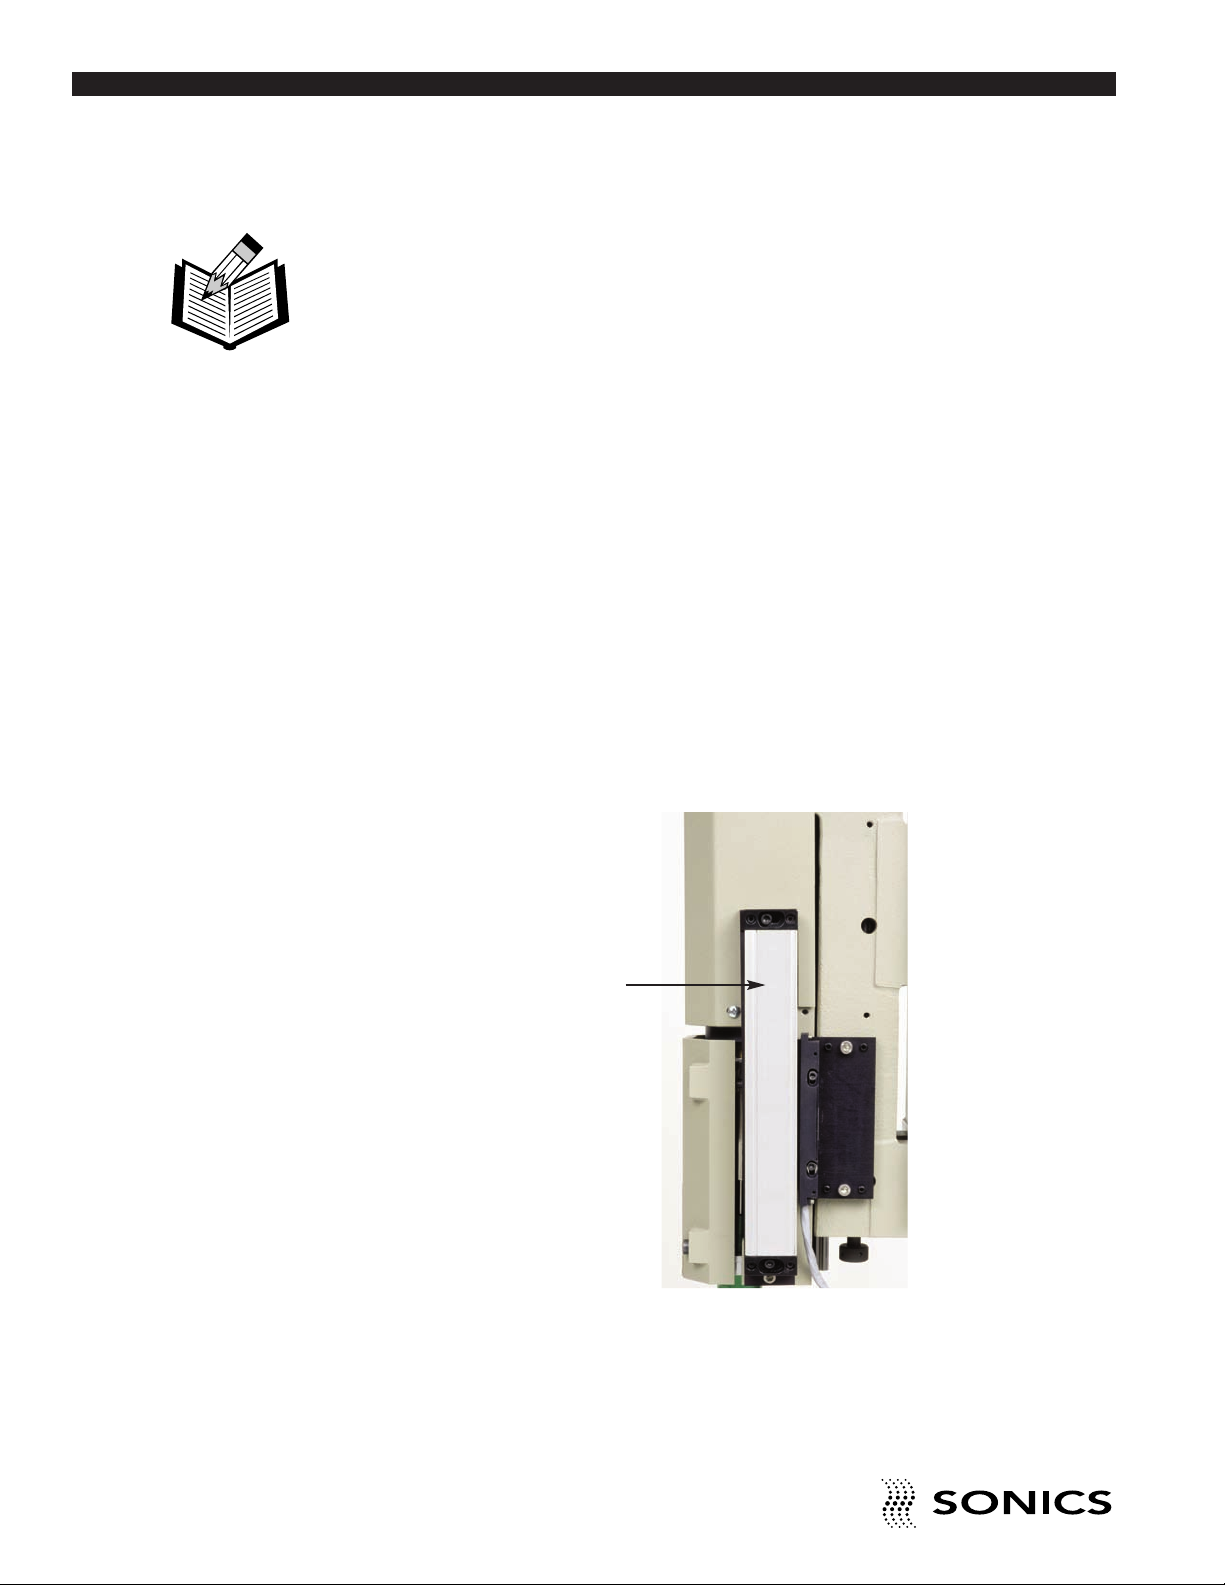
A Linear Encoder is available as an option. The Linear Encoder allows
distance-controlled welding in incremental and absolute modes.
The Linear Encoder is supplied with a 9-pin male connector that connects to
a matching 9-pin female connector on the power supply (factory installed).
LINEAR ENCODER
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
10
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 12
O P E R A T I N G P R O C E D U R E S
Go To Top Of Document
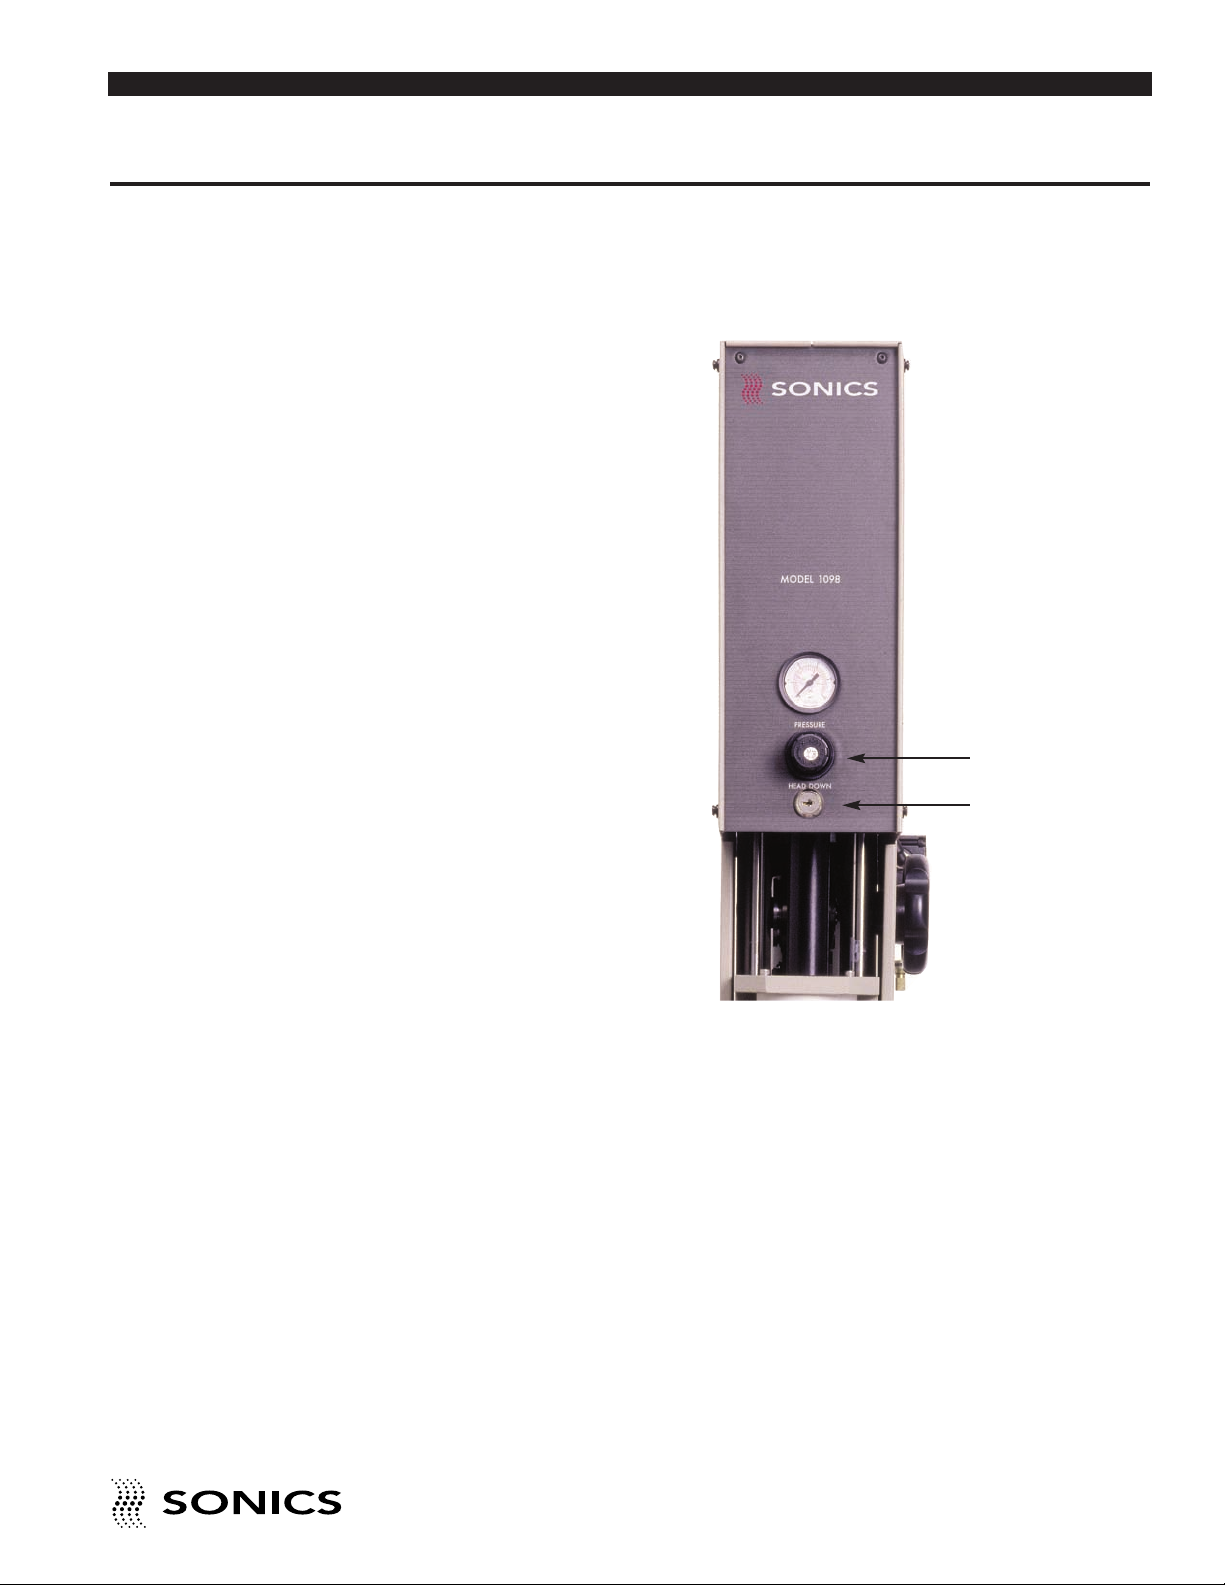
CONTROL PANEL
Located above the converter housing on the 1098 press are the following
controls:
❶
❷
1. Black PRESSURE REGULATOR with corresponding gauge that allows
regulation of the (air) pressure with which the horn contacts the part(s). Pull
the knob to make adjustments, and then push in to lock setting when
desired pressure is displayed on the gauge. Once pulled, turning the knob
clockwise increases pressure, and turning it counterclockwise decreases
pressure.
2. HEAD DOWN KEY SWITCH which when turned clockwise allows the
head to move down under gauge pressure. (This action does not cause
ultrasonics to be activated.)
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
11
Page 13
I N I T I A L E Q U I P M E N T S E T U P
Go To Top Of Document
ASSEMBLING AND MOUNTING CONVERTER, BOOSTER,
AND HORN
If the converter, booster, and horn are not already assembled, follow these
instructions:
1. Clean the mating surfaces of the converter and booster, as well as the
Never tighten the horn to
the booster using the
housing door as the upper
wrench as this may cause
damage to the booster
and/or converter.
threaded stud and hole. Check that the stud is tight (see recommended
torque requirements on page 13).
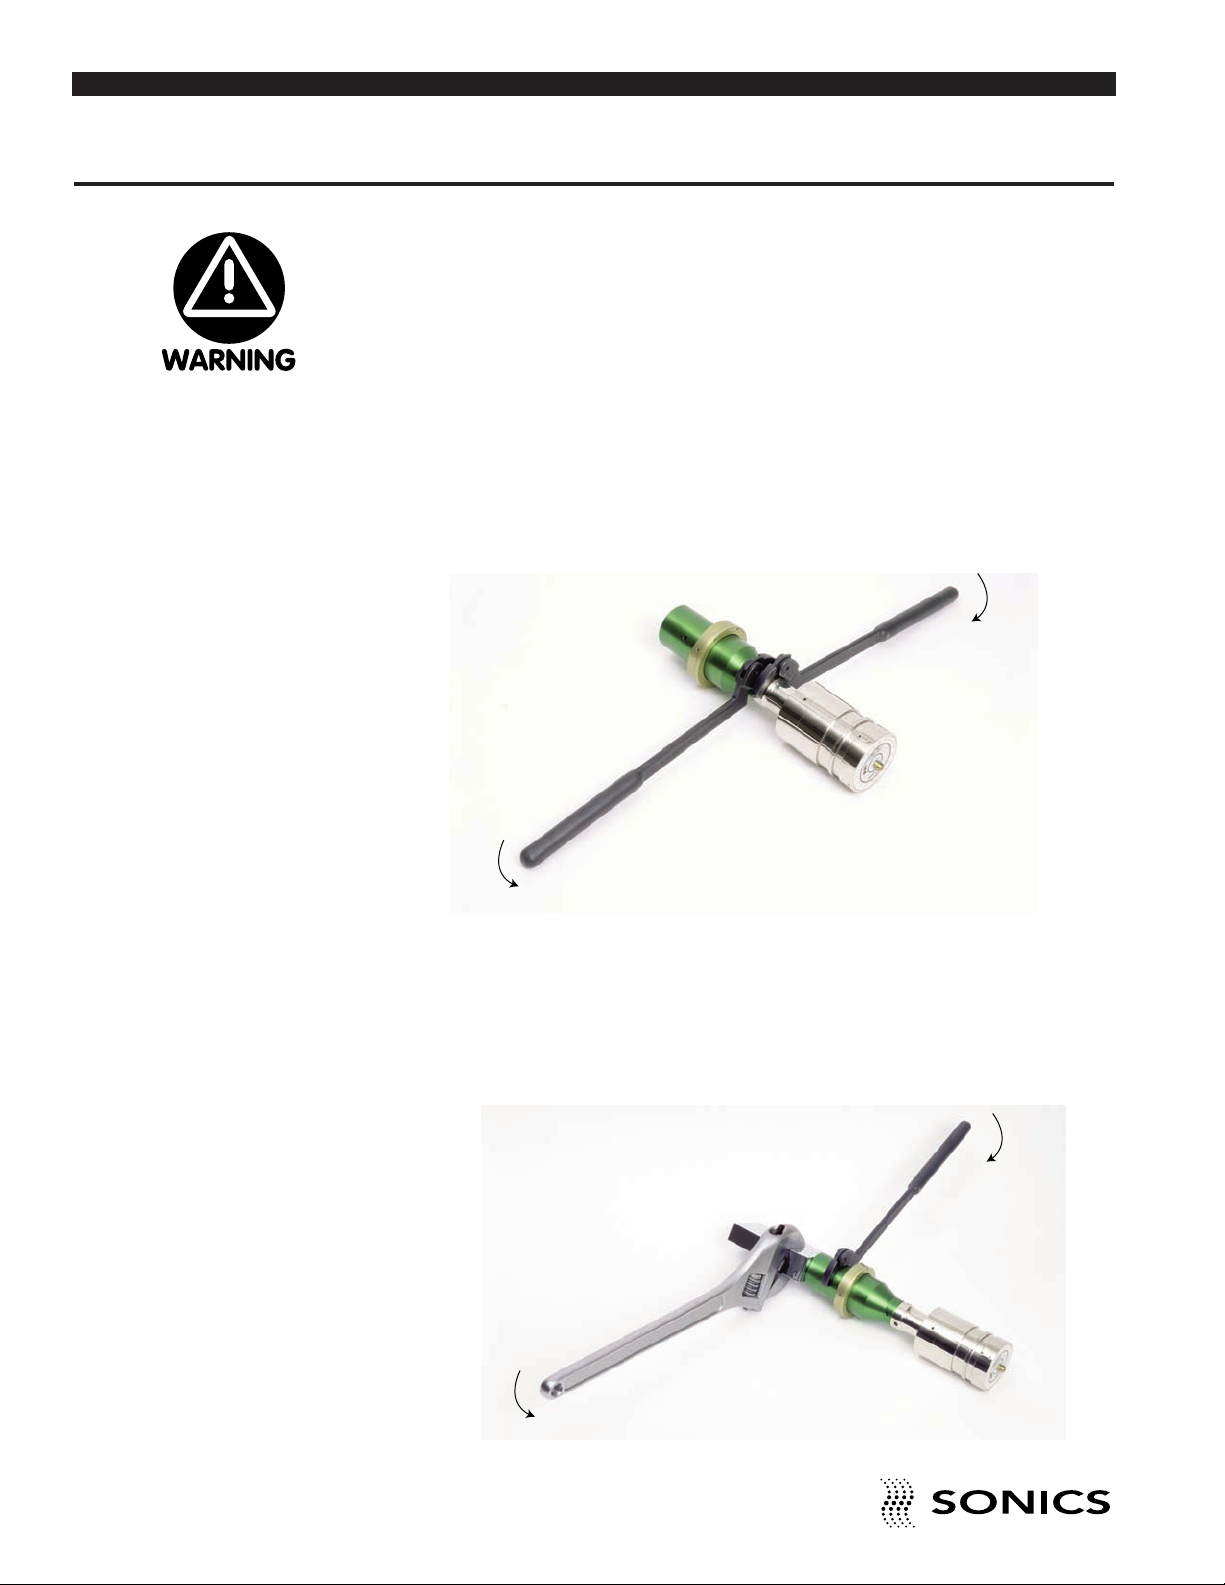
2. Hand assemble the converter and booster together. Using spanner
wrenches as shown below, tighten until snug. Then, using a torque wrench,
tighten to 25-35 foot-lbs. (34-47 newton-meters). Do not force or
overtighten.
CONVERTER/BOOSTER
3. Clean the mating surfaces of the booster and horn, as well as the threaded
stud and hole. Check that the stud is tight. (See recommended torque
requirements on next page.)
4. Hand assemble the horn to the booster. Using a spanner and an open-ended
wrench as shown below, tighten securely. Then, using a torque wrench,
tighten to 25-35 foot-lbs. (34-47 newton-meters). Do not overtighten.
CONVERTER/BOOSTER/HORN
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
12
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 14
NOTE: When performing
Go To Top Of Document
any of the operations
described on this page and
pages 14-15, DO NOT turn
on the power supply.
5. Using the 3/16” (4.7 mm) T-handle wrench provided, loosen (turn
counterclockwise) the two cap screws screws on the hinged converter
housing and open the door.
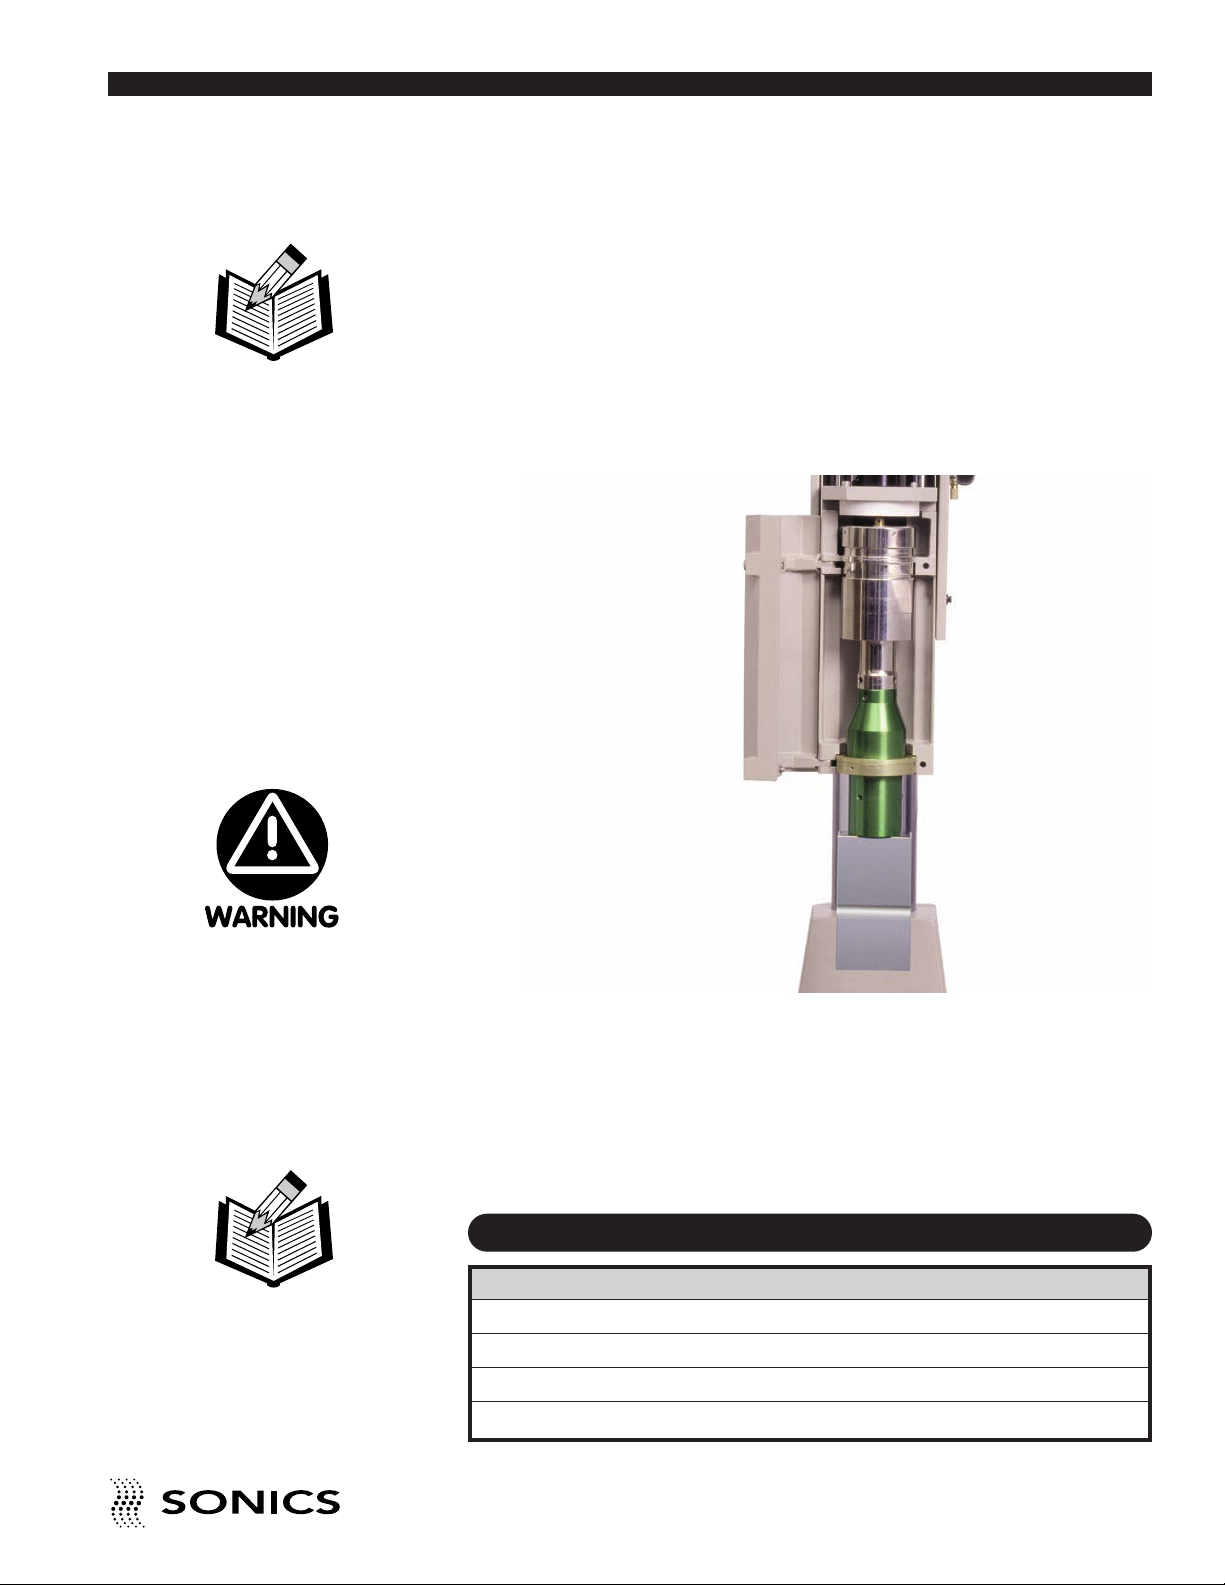
6. Place the converter / booster / horn assembly in the housing with the horn
facing down. Fit the male brass button on the top of the converter into the
female brass fitting in the bottom of the contact block assembly housing,
and gently push the assembly up and in so that the booster mounting ring
rests on the lower support ridge.
CONVERTER / BOOSTER /
HORN ASSEMBLY
Never tighten the horn to
the booster using the
housing door as the upper
wrench as this may cause
damage to the booster
and/or converter.
NOTE: If you do not close
the housing door once the
assembly is in place, the
assembly can fall out.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
7. Close the converter housing door and tighten (turn clockwise) the two
socket head cap screws just until they are snug. Do not tighten the horn to
the booster using the door as the upper wrench. Hand-forcing the horn on
and off in this manner can twist wires and cause a failure. If the horn is not
in the correct position to make contact with your material, re-position the
converter.
RECOMMENDED TORQUE REQUIREMENTS
Component Foot-Lbs. Newton-Meters
Converter / Booster 25 - 35 34-47
Booster / Horn 25 - 35 34-37
Stud 45 61
Tips 25 - 35 34-47
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
13
Page 15
Support the head before
Go To Top Of Document
releasing the column
clamps so that it cannot
crash down or fly up.
Ignoring this warning might
result in injury and/or
damage to the equipment
and part being welded.
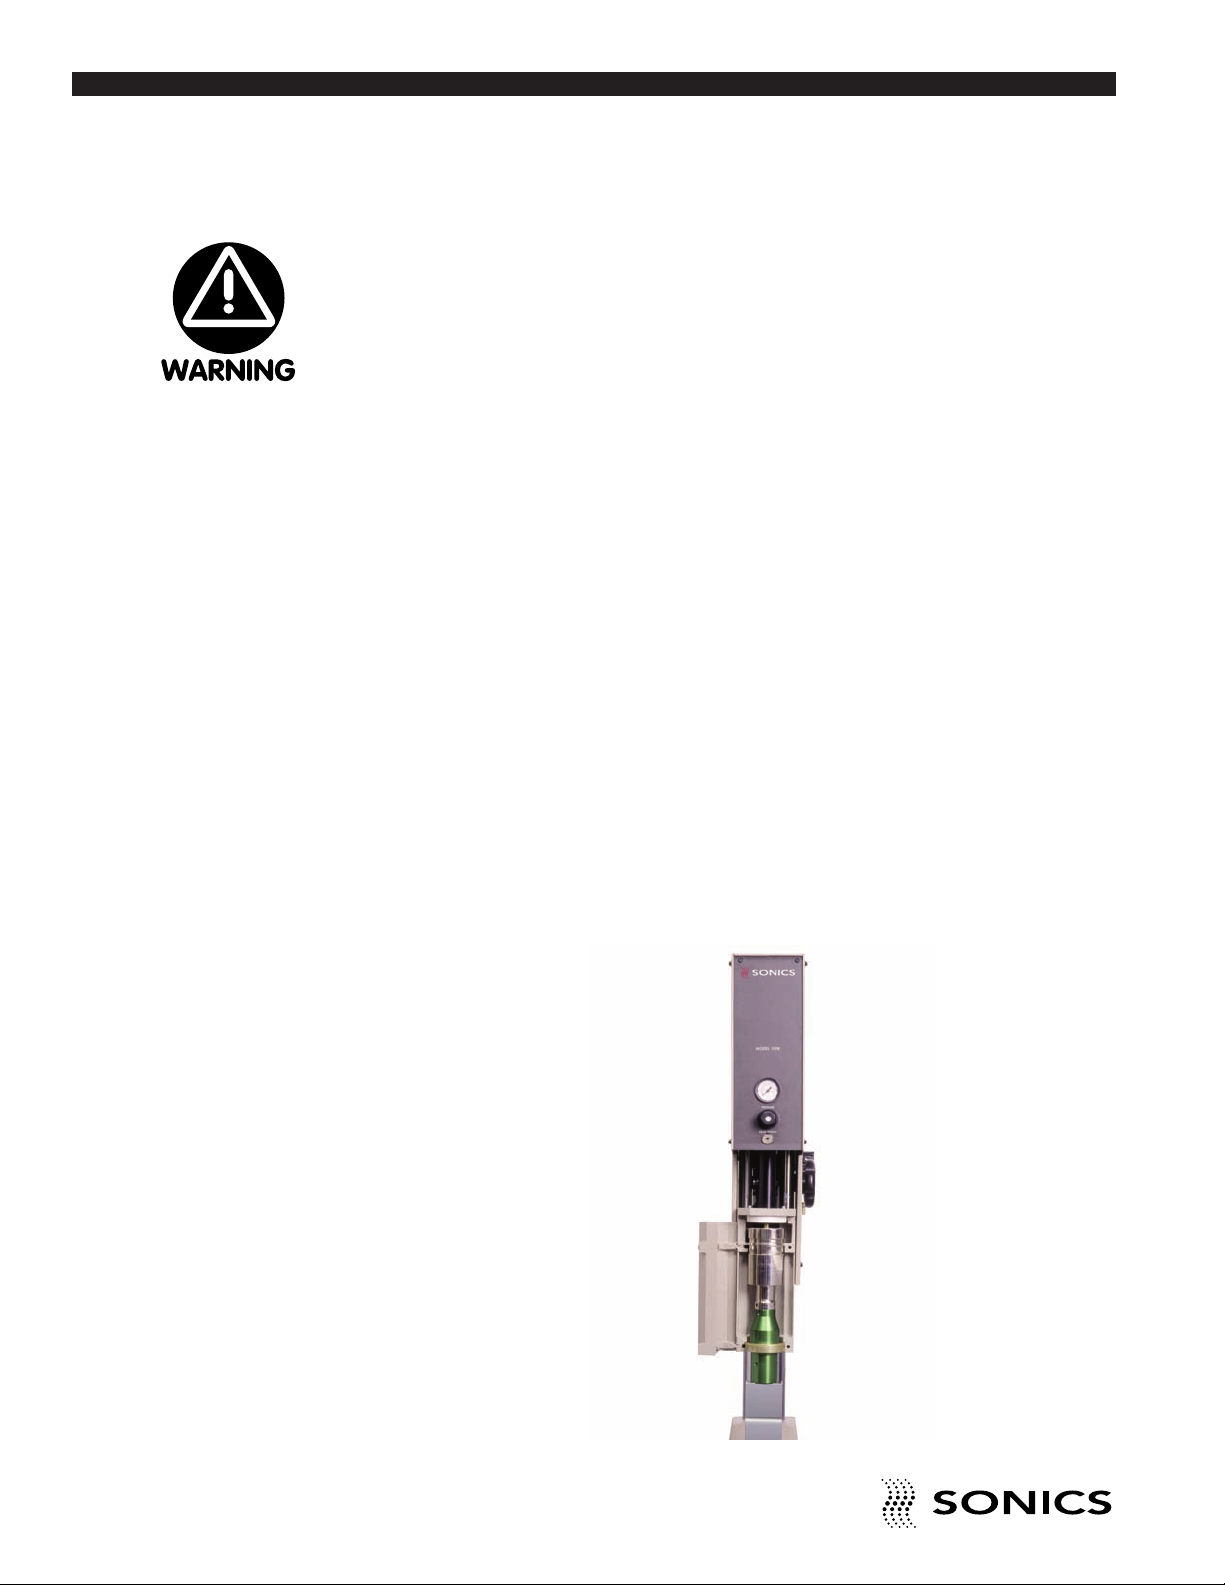
HORN AND FIXTURE ALIGNMENT
For maximum productivity, the clearance between the horn and the part
should be at a minimum. However, adequate clearance should be provided to
enable easy loading and unloading of the part from the holding fixture. The
maximum stroke distance is 4" (101.6 mm). Ensure that the horn does not
contact the part when the head is close to the limit of its down travel distance.
Otherwise, the horn may not have sufficient distance to travel downwards to
achieve a full depth of weld. Set welding height as follows:
First, position the holding fixture loosely on the base plate using 3/8-16
screws. Then, place the part to be welded in the fixture.
1. Insert key and turn the HEAD DOWN key switch clockwise to allow head
movement. Then, before loosening the column clamps, hold onto the head
assembly firmly as it can move rapidly up or down with heavy tooling once
the clamps are released. While holding the head assembly, loosen the two
column clamps (counterclockwise) and move the head up or down as
required. Then tighten the column clamps.
2. Using the PRESSURE REGULATOR (turn counterclockwise) and
corresponding gauge, set the air pressure to zero.
3. Loosen the column clamps once again and manually lower the head until
the horn contacts the part. Tighten the clamps.
4. Loosen the cap screws on the converter housing door and gently rotate the
head and horn as required to ensure proper horn-to-part alignment.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
14
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 16
NOTE: For maximum
Go To Top Of Document
safety and productivity,
adjust the clearance
between the horn and the
part to a minimum that will
still allow ease of loading
and unloading.
5. Lock the two column clamps, tighten the converter housing door screws,
and then tighten the fixture on the base plate.
6. Check for proper mating of fixture, parts, and horn. If the horn and part are
not in parallel contact, shim the fixture or adjust leveling screws as
required.
7. Set the PRESSURE regulator to a reading of 20 psig (140 kPa/1.4 bar) on
the pressure gauge. (Turn the PRESSURE knob clockwise.)
8. To check that the horn and parts are properly aligned, the horn needs to
be lowered. Read through the Operation instructions on page 16, and then
proceed to lower the horn as detailed. If the horn and parts are not
sufficiently aligned, then repeat steps 4 through 8. However, if you are
working with small, delicate parts, then fine adjustments can be made
using the positive stop adjustment knob as explained below.
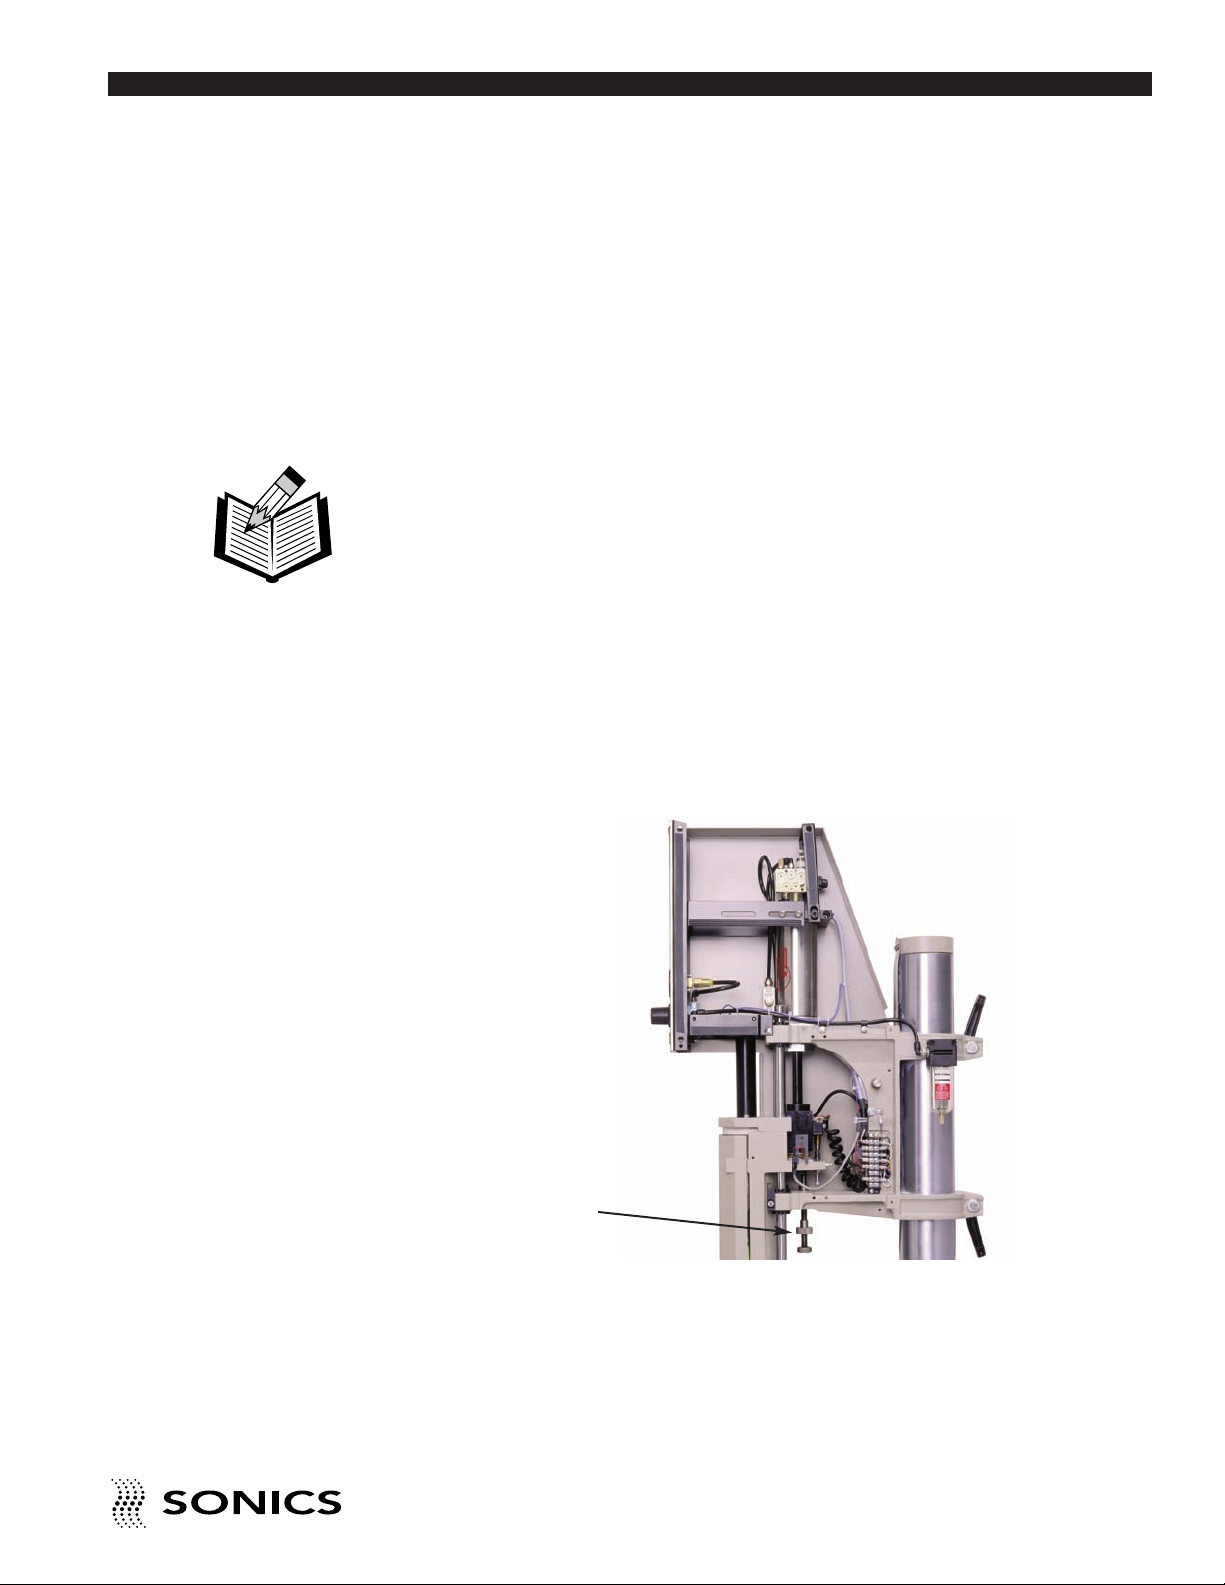
POSITIVE STOP ADJUSTMENT
The positive stop is set to limit the downward travel of the horn to
approximately 75%. Readjustments may be required. Coarse adjustment of
the clearance between the face of the horn and part should be made using
the elevation control. Fine adjustment should be made using the positive stop.
POSITIVE STOP
ADJUSTMENT
KNOB
The positive stop adjustment knob is located offset from the converter
housing. Turning the knob clockwise will decrease downward travel distance.
Turning the knob counterclockwise will increase the downward travel
distance. Rotate the knurled thumbscrew to lock and unlock the positive stop.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
15
Page 17
O P E R A T I O N
Go To Top Of Document
ACTUATION
The 1098 press is equipped with two maintained anti-repeat (non-tie-down)
palm buttons, one located on the left and one on the right side of the base of
the press. Both palm buttons must be pressed simultaneously to activate the
press to cycle the welder. To operate the press, follow these simple steps:
The equipment has safety
devices that require both
hands to be on the palm
buttons until the horn
contacts the workpiece. Do
not defeat or modify
these safety devices.
NOTE: Power supply
cannot be shut off once the
weld cycle has started.
Termination of cycle can
only be achieved by using
the EMERGENCY STOP
button.
1. Depress both black palm buttons simultaneously.
2. Once the horn comes in contact with the part and the ultrasonics are
activated, release the palm buttons. If you release the buttons before
contact is made, the head will immediately return to its “home” position.
EMERGENCY STOP
To abort the 1098 press during welding, simply press the red EMERGENCY
STOP button located at the front center of the press base.
Once the EMERGENCY STOP button has been depressed, the head will
retract and return to its “home” position. Simply rotate the EMERGENCY
STOP button to the right 1/4 turn to release the press for further operation.
Do not use with a
footswitch unless alternate
means of pinch-point
protection is provided.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
16
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 18
F I N E A D J U S T M E N T S
Go To Top Of Document
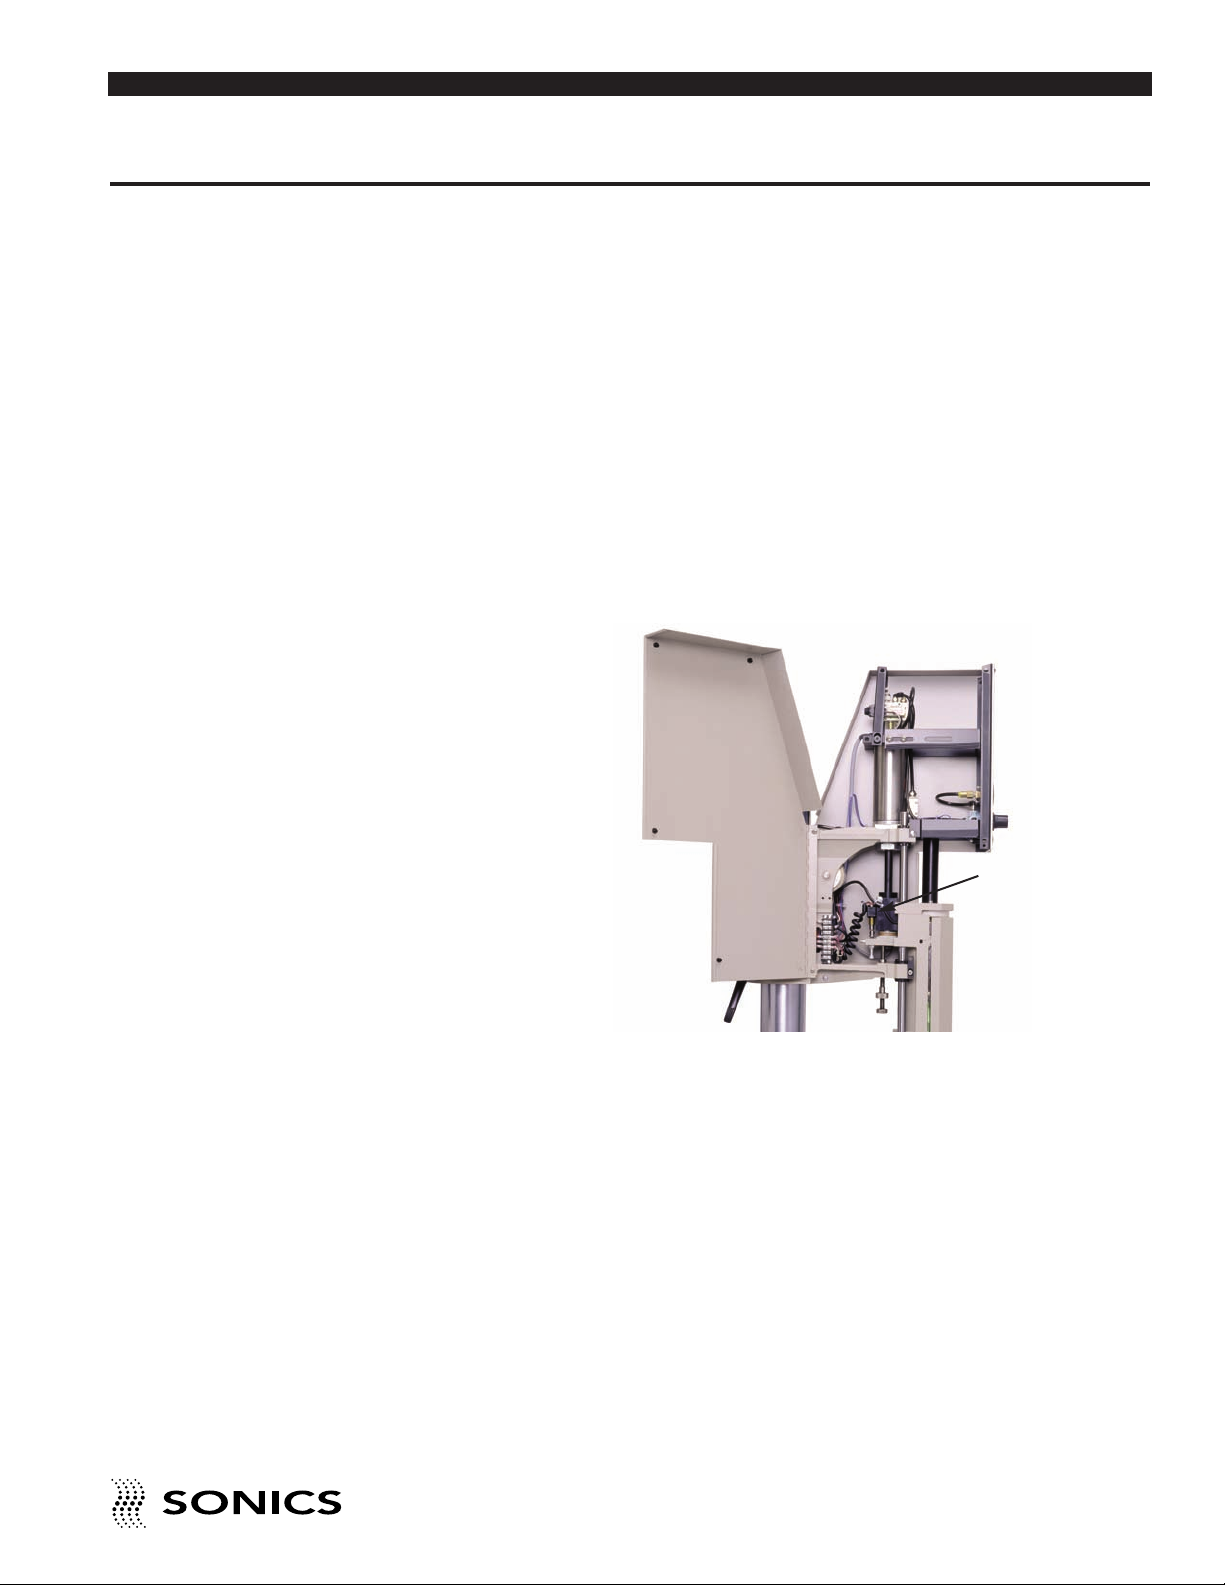
PRESSURE SWITCH ADJUSTMENT
For systems mounted in the normal vertical position with downward travel, no
adjustment should be necessary. The minimum trigger pressure is factory set
at 4-7 psig.
However, if the minimum trigger pressure requires recalibration or readjustment, observe the following procedure:
1. Maintain air pressure and unplug the power supply from the electrical
source.
2. Release the four latches to open the hinged side cover.
3. Loosen the jam nut holding the 1/4-20 cap screw in place.
4. Rotate the small, knurled, threaded rod upward until the Pressure Switch
closes.
PRESSURE
SWITCH
5. Next rotate the cap screw down until the Pressure Switch opens.
6. Rotate cap screw down one turn past the Pressure Switch open position.
7. Tighten the jam nut to lock cap screw in position.
8. Close the hinged side cover and secure latches.
9. Plug the power supply into the electrical source.
10. Cycle the welder.
The press is now set to trigger at the minimum trigger pressure of 4-7 psig.
A press actuating in an upward or horizontal direction should be set to trigger
at a minimum of 8-10 psig. Lower values may affect trigger performance
where false triggering may be observed.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
17
Page 19
NOTE: Consult the
Go To Top Of Document
Applications Manual or call
our Applications Lab for
proper booster selection.
BOOSTER SELECTION
The first step in optimizing welding conditions is to select a booster which will
provide the necessary amplitude. For parts one inch (25.4mm) in diameter or
greater, start with a moderately high amplitude booster such as a gold. For
smaller parts, start with a green booster. Determine optimum amplitude by
welding a few parts, and repeat the procedure with boosters giving higher or
lower amplitude. If there appears to be little or no difference, use the booster
giving the highest amplitude.
Seven standard boosters, color coded or engraved for ease of identification,
are available either to increase or decrease the amplitude.
BOOSTER
Color Part No. Gain Amplitude Effect
Black BHN15TBK 2.50 Increase
Silver BHN15TSI 2.00 Increase
Gold BHN15GD 1.50 Increase
High gain boosters, such
as silver and black in
combination with high gain
horns can result in the horn
cracking or failing.
Brown BHN15BR 1.25 Increase
Green BHN15GR 0 No Change
Purple BHN15PU 0.75 Decrease
Blue BHN15BU 0.50 Decrease
PRESSURE
During the welding process, sufficient pressure should be applied to the part
so that the mating surfaces contact each other. If the pressure is too low, the
process will run inefficiently causing unnecessarily long weld time cycles,
marking of the parts or poor welding. If the pressure is too high, the horn may
stop vibrating, the part(s) might fracture, or the power supply might overload.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
18
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 20
Excessive velocity may be
Go To Top Of Document
unnecessary and harmful
to the system.
STROKE SPEED ADJUSTMENT
The velocity at which the horn descends and returns can be adjusted via the
speed controls. These controls are factory adjusted for average operating
conditions and should not require further adjustment. However, if a minor
adjustment is necessary, adjust in small degrees. Turn clockwise to slow the
extend speed, and counterclockwise to increase the return speed.
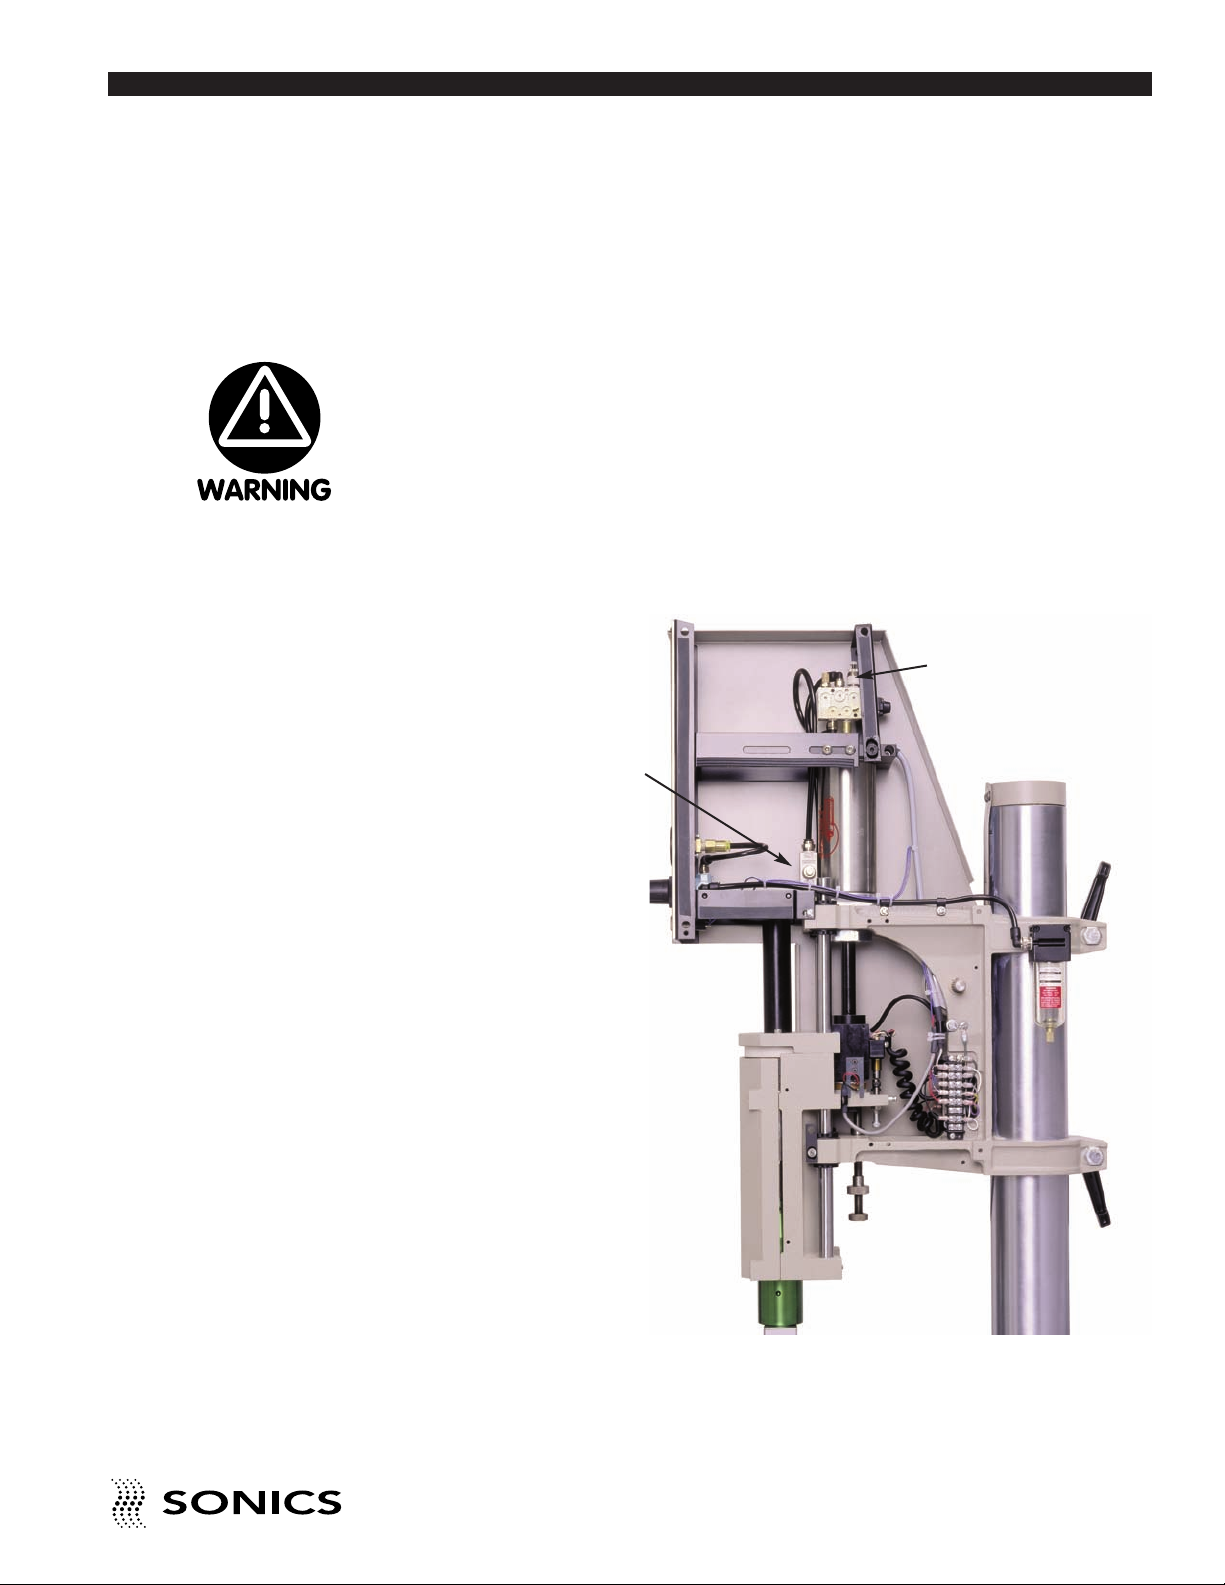
The speed controls are 2 small threaded screws located in the top of the
press as shown below.
Turn the Extend Speed Control screw clockwise to slow the extend speed,
counterclockwise to increase the speed. Turn the Return Speed Control screw
clockwise to slow the return speed, counterclockwise to increase speed.
RETURN SPEED
CONTROL
EXTEND
SPEED
CONTROL
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
19
Page 21
NOTE: Contact between
Go To Top Of Document
the booster and horn
should be parallel. When
encountering symptoms
such as loud noises or
tuning difficulties, examine
the booster / horn
interfaces for parallelism,
corrosion, galling or foreign
deposits. Also check the
tightness of the stud.
RE-ESTABLISHING PROPER BOOSTER / HORN
INTERFACES
To re-establish proper interfaces, follow these instructions:
1. Using open-ended wrenches, separate the booster from the horn. Clean
each item and then examine interfaces for irregularities (scoring).
2. If irregularities are present, remove the stud.
3. Tape a sheet of 400 grit emery cloth to a smooth, flat surface. (Do not use
coarser than 400 grit.)
4. Grasp the lower portion of the booster or horn and move it across the
emery cloth. To ensure proper lapping, a) hold the part straight, b) apply
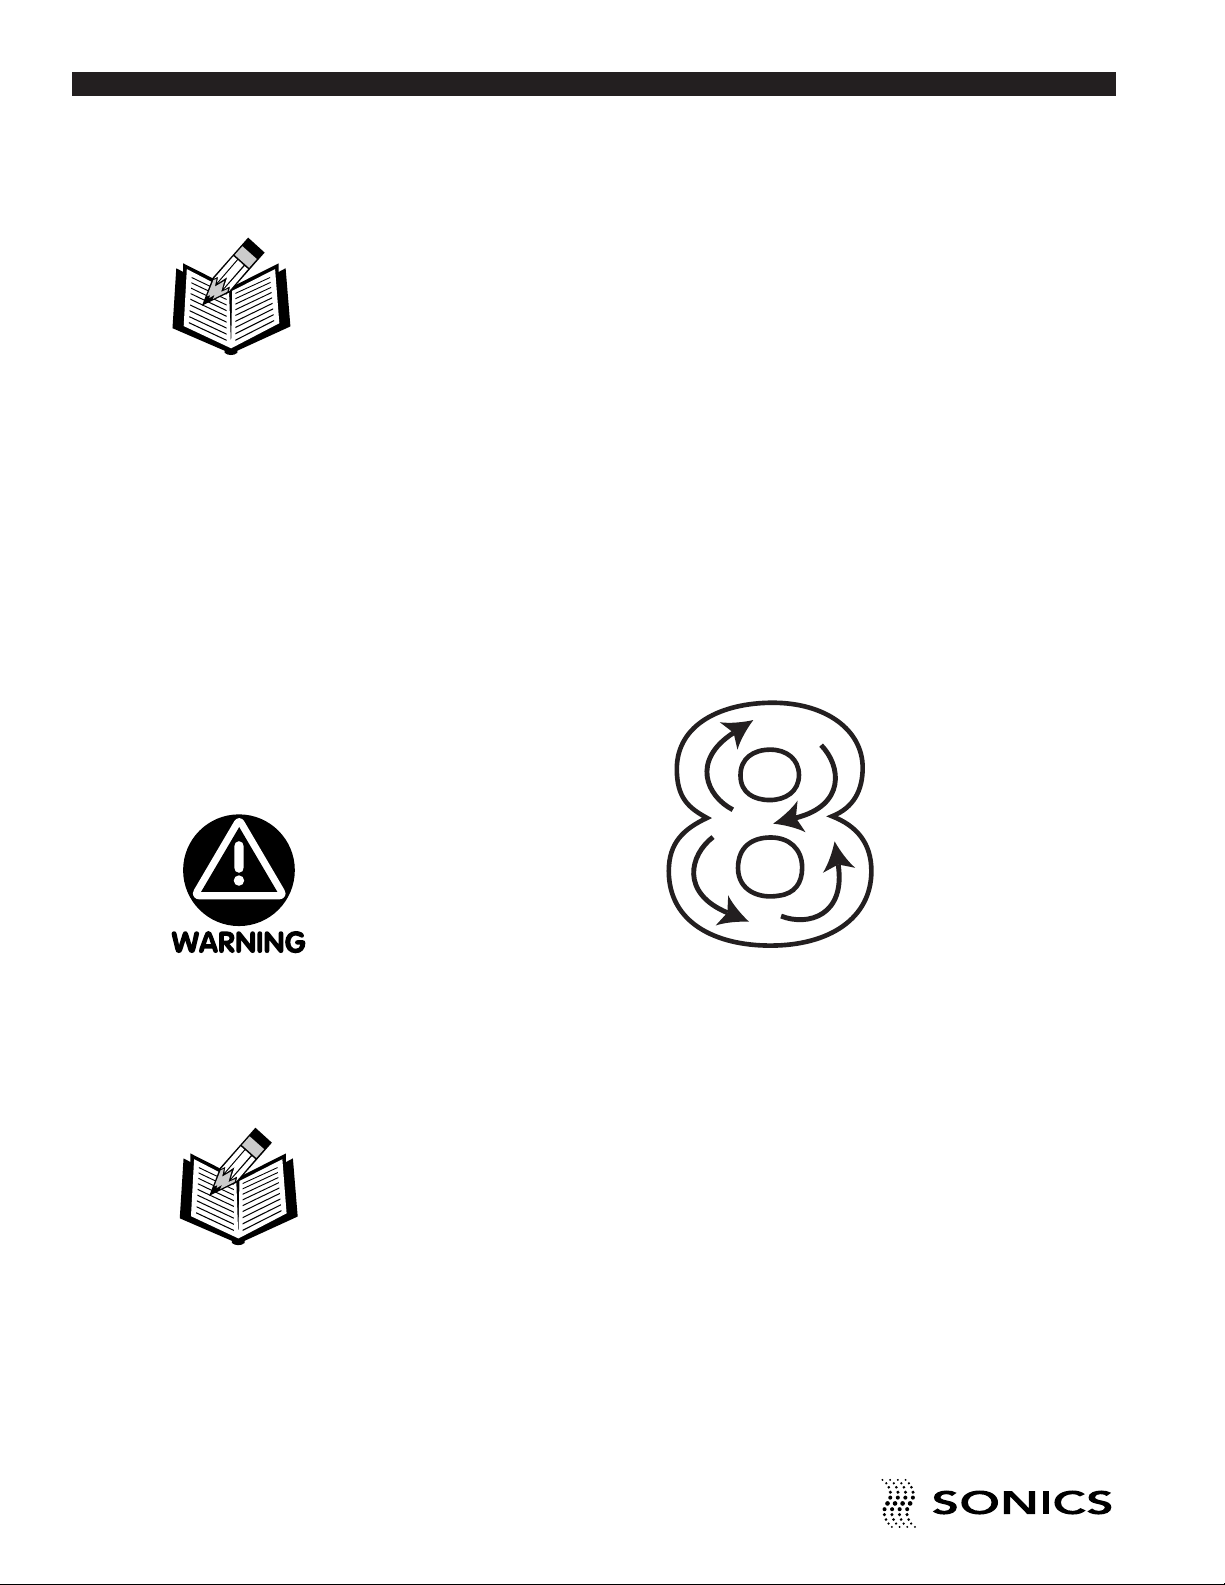
light downward pressure, and c) move in one direction only in a figure 8
pattern.
Repeat the figure 8 pattern once more.
DO NOT use anything
coarser than 400 grit
emery cloth.
5. Then, rotate the booster or horn 1/3 of a turn in a clockwise direction and
then repeat step 4.
6. Repeat step 5.
7. Using wire brush, clean stud, then replace securely. Tighten new stud to
the recommended torque specifications on page 13.
NOTE: Machining of
booster / horn may alter
the ability to tune the
component to the system.
System inoperation may
occur.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
20
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 22
M A I N T E N A N C E
Go To Top Of Document
NOTE: If packing unit for
return shipment, DO NOT
use styrofoam “peanuts.”
REPAIRS / SERVICE
If problems are encountered, contact our Service Department as follows:
Phone: 1-800-745-1105 • 1-203-270-4600
Fax: 1-203-270-4610
E-Mail: [email protected]
It is suggested that a system in need of repair be sent back to the factory, with
a written description pertaining to the nature of the problem.
Always contact the factory for return authorization before shipping any
instrument. Include date of purchase, model number, and serial number. For
units not covered by the warranty, a purchase order should be forwarded to
avoid unnecessary delay. Care should be exercised to provide adequate
packing to insure against possible damage in shipment. The system should
be sent with all transportation charges prepaid and return method of shipment
indicated.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
21
Page 23
W A R R A N T Y
Go To Top Of Document
Sonics & Materials, Inc., hereinafter referred to as “Sonics,” warrants its
products for a period of one year from the date of shipment against defect in
material and workmanship under normal installation, use, and maintenance
as described in the operating instructions which accompany such equipment.
During the warranty period, “Sonics” will, at its option, as the exclusive
remedy, either repair or replace without charge for material and labor, the
part(s) which prove upon our examination to be defective, provided the
defective unit is returned to us properly packed with all transportation charges
prepaid.
Ultrasonic welding horns constructed of titanium or aluminum are guaranteed
against defects for a period of one year from date of shipment. “Sonics” will
repair or replace a cracked or defective horn once without charge, if failure
occurs within the warranty period.
Ultrasonic welding horns constructed of steel are guaranteed against defects
for a period of ninety days from date of shipment. “Sonics” will repair or
replace a cracked or defective steel horn once at a charge of 50% of the
original purchase price, if failure occurs within the warranty period.
LIMITATION OF WARRANTY
This warranty is in lieu of any other warranties, either express, implied, or
statutory. “Sonics” neither assumes nor authorizes any person to assume for
it any other obligation or liability in connection with the sale of its products.
“Sonics” hereby disclaims any warranty or merchantability or fitness for a
particular purpose. No person or company is authorized to change, modify,
or amend the terms of this warranty in any manner or fashion whatsoever.
Under no circumstances shall “Sonics” be liable to the purchaser or to any
other person for any incidental or consequential damages or loss of profit or
product resulting from any malfunction or failure of this “Sonics” product.
This warranty does not apply to equipment which has been subject to
unauthorized repair, misuse, abuse, negligence or accident. Equipment
which, in our judgment, shows evidence of having been used in violation of
operating instructions, or which has had the serial number altered or
removed, will be ineligible for service under this warranty.
No liability is assumed for expenses or damages resulting from interruptions
in operation of the product or damages to material in process.
“Sonics” equipment is designed for maximum operator safety and
incorporates built-in safety devices. Any modifications to these safety features
will void the warranty. “Sonics” assumes no responsibilities for consequential
damages incurred due to modifications to the said equipment.
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
22
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 24
“Sonics” reserves the right not to warrant horns of unusual or experimental
Go To Top Of Document
design which in our judgment are more likely to fail in use.
This warranty does not cover equipment used for applications requiring metalto-metal contact with weld time in excess of 1 second.
Data supplied in the instruction manual has been verified and validated and
is believed adequate for the intended use of the equipment. If the equipment
or procedures are used for purposes other than those specified herein,
confirmation of their validity and suitability should be obtained in writing from
“Sonics.”
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
23
Page 25
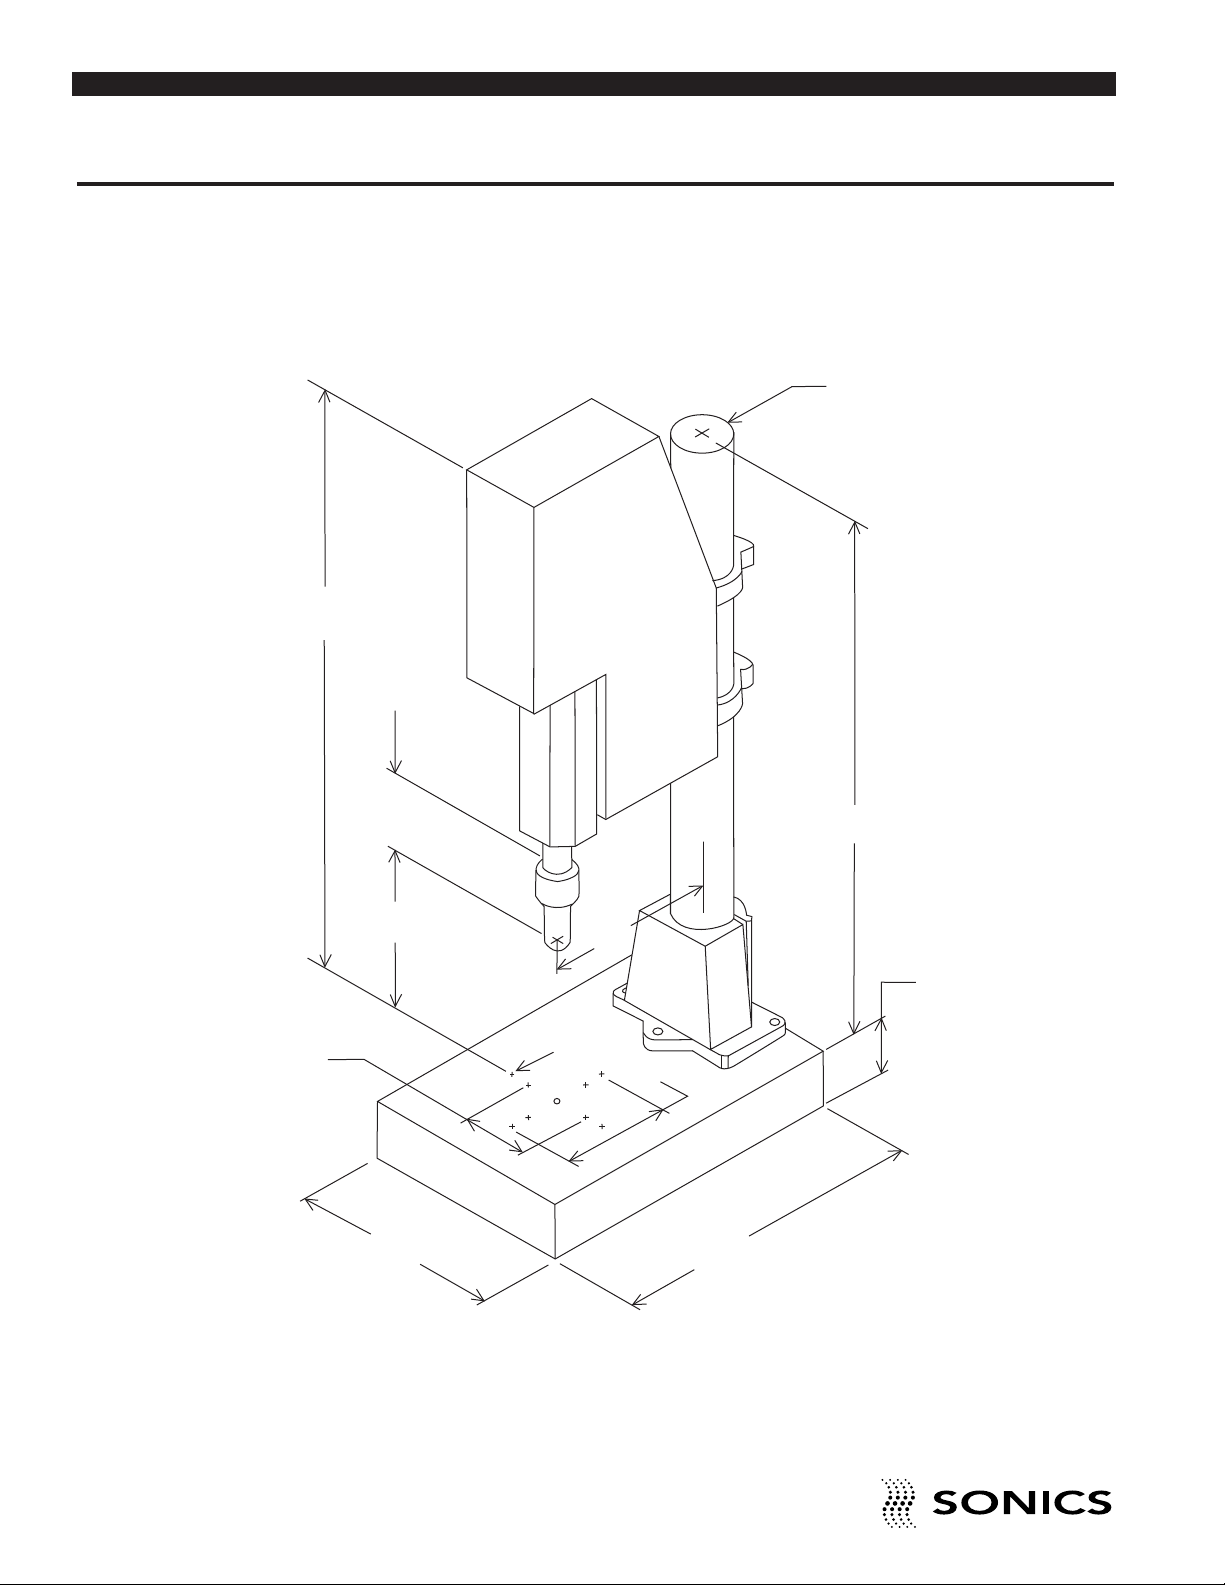
47 (MAX) (1193.8)
31/2 DIA. (88.9)
351/4 (895.3)
3
3
/4 (95.2)
7 (177.8)
211/16 (534.9)
141/8 (358.7)
47/16 (112.7)
141/2 (MAX)
(368.3)
51/4 (TYP)
(133.3)
11
1
1
/6
4
(2
83
.7
)
3
/8-16 (8) (TYP)
A P P E N D I X
Go To Top Of Document
1 0 9 8 L A Y O U T
Dimensions are shown in inches and millimeters,
i.e., 11/2 (38.1) signifies 11/2" (38.1mm)
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
24
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
Page 26
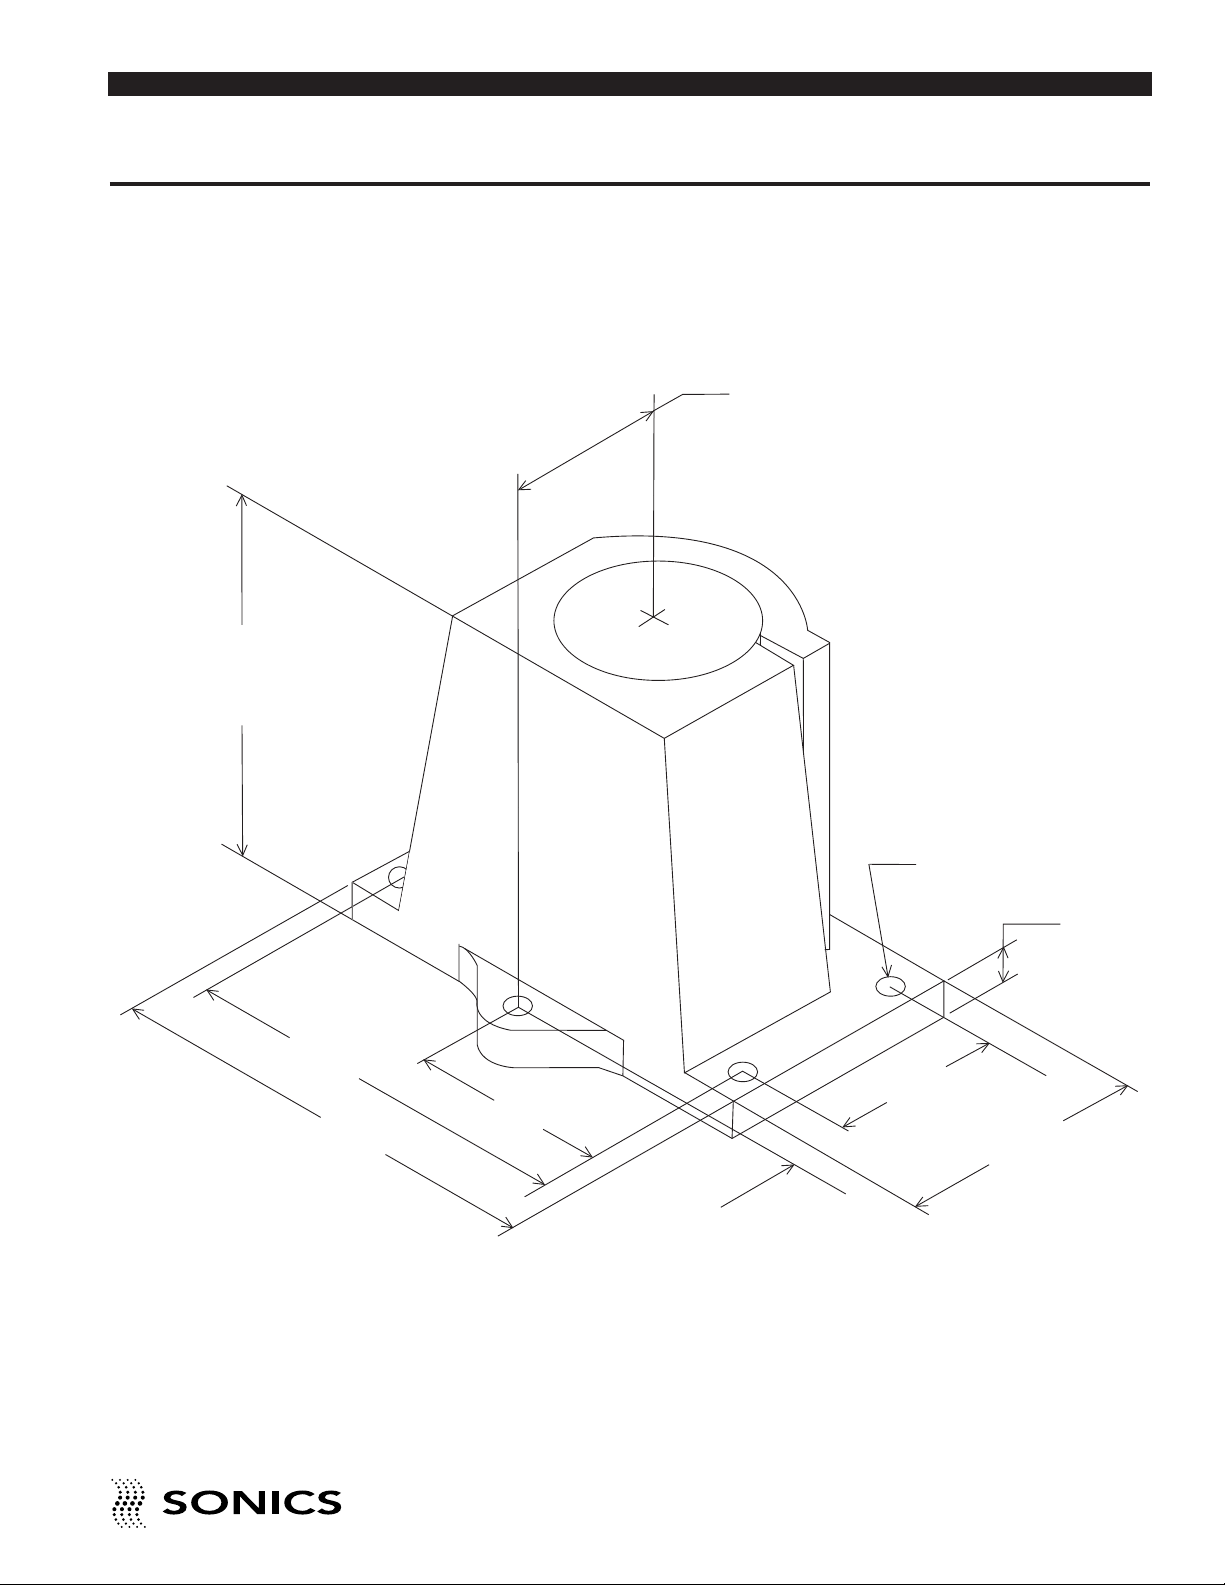
A P P E N D I X
3
5
/16
(84.1)
7 (177.8)
8 (203.2)
9 (228.6)
4 (101.6)
3
1
/2 (88.9)
1
15
/16 (33.3)
5 (127.0)
17
/32 DIA. (5 PLCS)
(13.4)
3
/4 (19.0)
Go To Top Of Document
M O U N T I N G H U B L A Y O U T
Dimensions are shown in inches and millimeters,
i.e., 11/2 (38.1) signifies 11/2" (38.1mm)
• • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • • •
I N S T R U C T I O N M A N U A L • MO D E L 10 9 8
25
Page 27
Sonics & Materials, Inc.
Corporate Headquarters European Office
53 Church Hill Road • Newtown, CT 06470 USA 22 ch du Vernay • CH - 1196 Gland, Switzerland
203.270.4600 • 800.745.1105 • 203.270.4610 fax (41) (0) 22/364 1520 • (41) (0) 22/364 2161 fax
 Loading...