

Page 1

PIPE NIPPLES
.
OUTSIDE DIAMETER
Seamless Pipe Nipples - Black & Galvanized
Standard Schedule 40, XH Schedule 80, Schedule 160, XXH
q FIG. 320:
Standard
Black Sch. 40
Specifications
Dimensions: ASTM A733 (See table below for standard sizes)
Threads: NPT per ASME B1.20.1
q FIG. 325:
Extra Heavy
Black Sch. 80
q FIG. 326:
160
Black Sch. 160
q FIG. 327:
XXH
Black
q FIG. 330:
Standard
Galv. Sch. 40
q FIG. 335:
Extra Heavy
Galv. Sch. 80
q FIG. 333:
160
Galv. Sch. 160
TOLERANCES
PIPE SIZE TOL.
1/8" - 1 1/2"
2" - 8"
±1/64
± 1% OF NOMINAL O.D
Material: ASTM A106 Grade B Seamless Pipe
ASTM A333 Grade 6 Seamless Pipe (For Canada only)
Finish: ASTM A106 Nipples Black or Hot Dip Galvanized
ASTM A333 Nipples Phosphate Coated or Zinc Electroplated
LENGTH ± 1/16"
Pipe
Size
in in in
1
⁄8 0.405
1
⁄4 0.540
3
⁄8 0.675 1 11⁄2 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1
⁄2 0.840 11⁄8 11⁄2 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
3
⁄4 1.050 13⁄8 11⁄2 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1 1.315 1
1
⁄4 1.660 15⁄8 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1
1
⁄2 1.900 13⁄4 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1
2 2.375 2 2
1
⁄2 2.875 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
2
3 3.500 2
4 4.500 2
5 5.563 3 4
6 6.625 3
Note: Other lengths available upon request.
8" Pipe Size available as POA - contact your Anvil Representative for details.
Pipe
O.D.
Length
Close
3
⁄4 11⁄2 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
7
⁄8 11⁄2 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1
⁄2 2 21⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1
⁄2 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
5
⁄8 3 31⁄2 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
7
⁄8 4 41⁄2 5 51⁄2 6 7 8 9 10 11 12
1
⁄8 41⁄2 5 51⁄2 6 7 8 9 10 11 12
Pipe Nipple Lengths
1
⁄2 5 51⁄2 6 7 8 9 10 11 12
q FIG. 329:
XXH
Galvanized
Nipples over
12" long have a
length tolerance
of +/- 1⁄8".
PROJECT INFORMATION APPROVAL STAMP
Project:
Address:
Contractor:
Engineer: Remarks:
Submittal Date:
Notes 1:
Notes 2:
PF-11.16
Approved
q
Approved as noted
q
Not approved
q
Page 2

PIPE NIPPLES
Specifications
Unless otherwise specified welded nipples ASTM A 53 are
furnished on orders for steel nipples in standard and extra
strong sizes 1⁄8" – 8" NPS
Welded steel nipples (A 53 Type F or Type E) are available in
standard and extra strong sizes 1⁄8" – 8" NPS
hand threads, black or galvanized.
Seamless nipples manufactured for the U.S. and International
markets are
manufactured for Canada
Seamless steel pressure tube nipples (ASTM A 106 Grade B) are
available in standard and extra strong sizes 1⁄8" – 8" NPS
(6 – 200 DN)
Right and left steel nipples are available in standard and extra
heavy weight sizes 1⁄8" – 4" NPS
6"
(152mm)
not
phosphate coated. Seamless nipples
with right hand threads, black only.
lengths.
(6 – 200 DN)
are
phosphate coated.
.
(8 – 50 DN)
(6 – 200 DN)
, in 4"
(102mm)
, right
and
Nipples are available from stock in
diameter, close to 12 NPS
NPS
(325 – 600 DN)
Steel pipe nipples meet ASTM A733.
1
⁄8" Schedule 40 and 80 galvanized nipples are all electroplated.
Identification
Where possible, each seamless pipe nipple is identified with
the following:
• A trade mark
• Seamless designation “SMLS”
• Pipe schedule 40, 80, 160, XXS
• Material designation
• Heat number for traceability
(300 DN)
. (Prices on application.)
1
⁄8" – 8" NPS
in length. Sizes 13" – 24"
(6 – 200 DN)
Standards and Specifications
Dimensions Material Thread Federal/Other
PIPE NIPPLES
Steel Pipe - Welded ASTM A733 ASTM A53 Type F or Type E ASME B1.20.1 WWN 351
Steel Pipe - Seamless (High Temp.) ASTM A733 ASTM A106 Gr. B ASME B1.20.1 WWN 351
Brass ASTM B687 ASTM B43 ASME B1.20.1 WWN 351
PF-11.16
Page 3
PIPE NIPPLES
Special Design Pipe Nipples
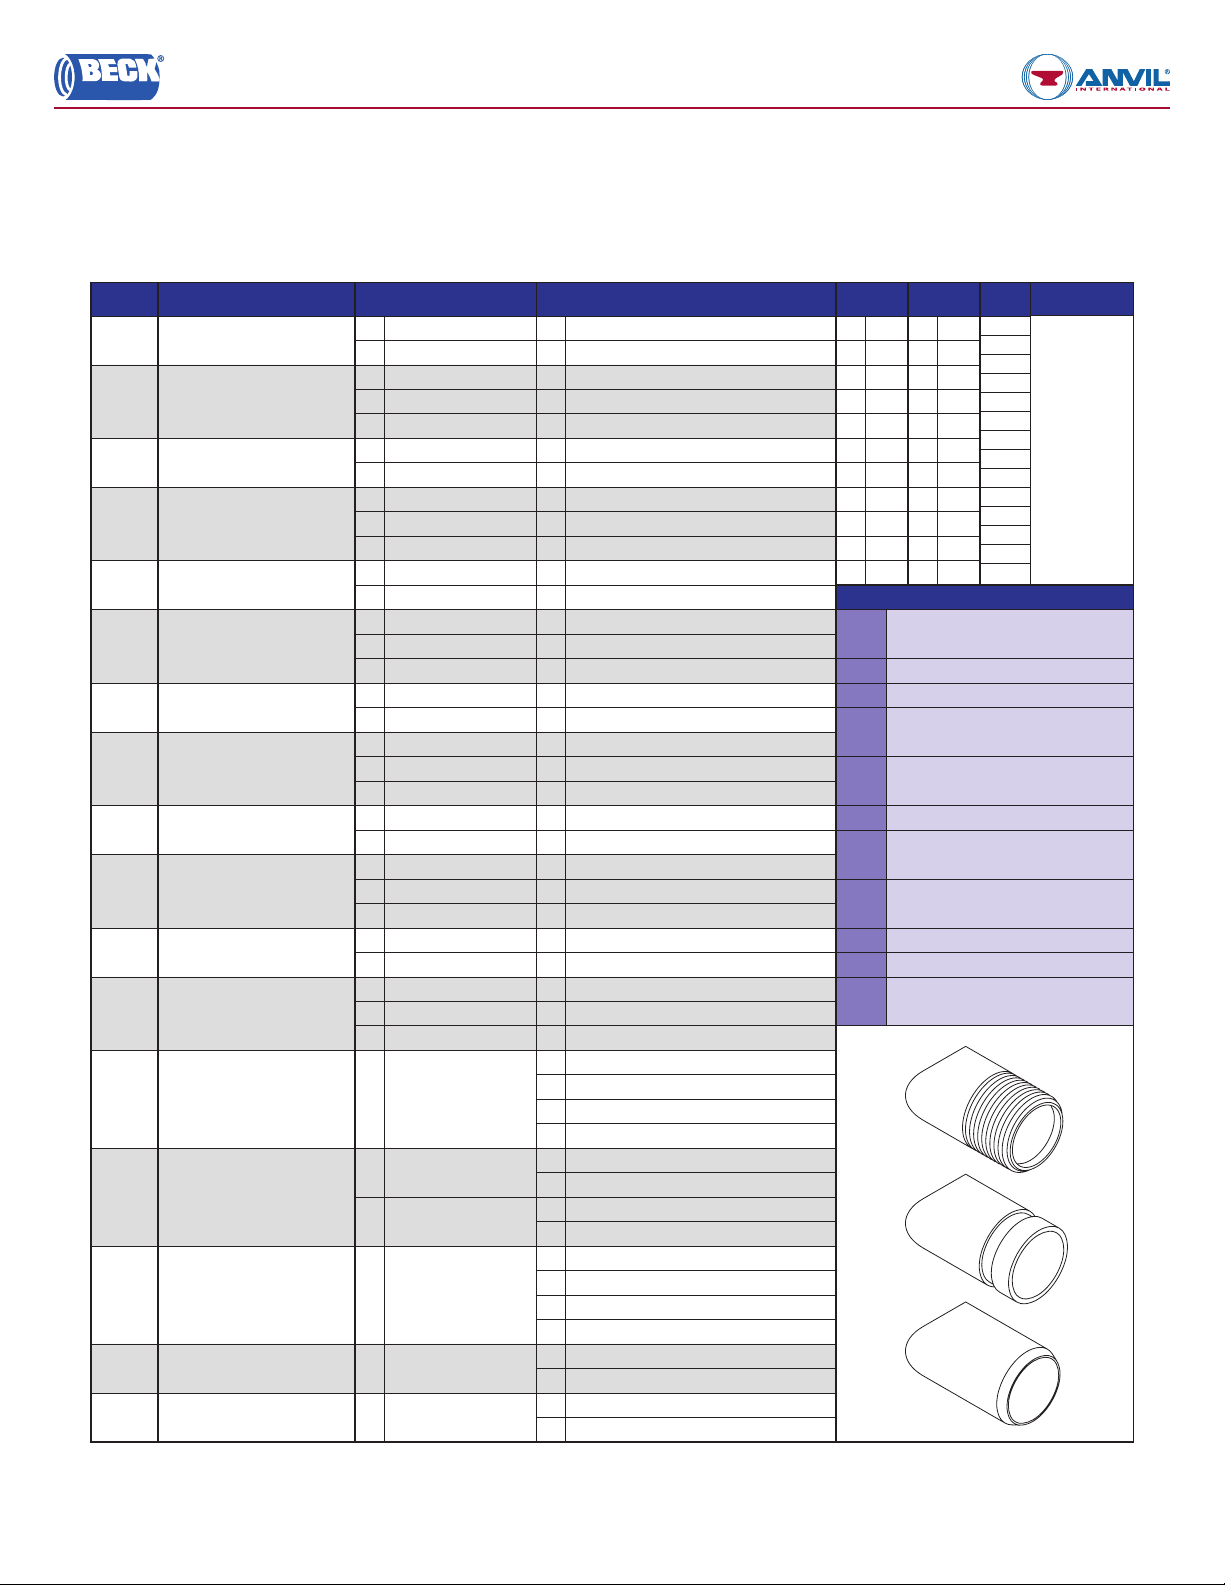
Beck Pipe Nipples are available with a variety of options for customization. To order, begin by selecting the figure number,
material, finish, and end treatments from the table below. Then, select the nominal pipe size and specify the length rounded to
the nearest 1/16". Contact your Anvil Representative for additional options.
Fig No.
320SD
330SD
325SD
335SD
326SD
333SD
327SD
329SD
339SD
343SD
338SD
342SD
341SD
344SD
345SD
362SD
363SD
** NPS and lengths available POA, upon request. Contact your Anvil Representative for details.
Description Material Finish End #1 End #2 NPS Length
Sch. 40 Seamless Nipple
Special Design
Sch. 40 Seamless Nipple -
Galvanized
Special Design
XH/Sch. 80 Seamless Nipple
Special Design
XH/Sch. 80 Seamless Nipple -
Galvanized
Special Design
Sch. 160 Seamless Nipple
Special Design
Sch. 160 Seamless Nipple -
Galvanized
Special Design
XXH Seamless Nipple
Special Design
XXH Seamless Nipple -
Galvanized
Special Design
Sch. 40 Welded Nipple
Special Design
Sch. 40 Welded Nipple -
Galvanized
Special Design
XH/Sch. 80 Welded Nipple
Special Design
XH/Sch. 80 Welded Nipple -
Galvanized
Special Design
Tank Nipple - Sch. 40
Welded
Special Design
**Butt Nipple - Sch. 40
Welded
Special Design
Mining Nipple - Sch. 40
Welded
Special Design
Special Design Seamless Nipple
Brass & Chromium Plated Brass
Special Design Grooved Adapter
Nipple - Aluminum & Brass
A ASTM A106 GR B A Plain with Zinc Phosphate Coating A NPT A NPT
B ASTM A333 B Plain with Sandblasted Surface B PLN B PLN
A ASTM A106 GR B A Hot Dip Galvanized per ASTM A153 C PSQ C PSQ
B ASTM A333 B Zinc Electroplated per ASTM B633 D PDB D PDB
- - C
A ASTM A106 GR B A Plain with Zinc Phosphate Coating F BEV F BEV
B ASTM A333 B Plain with Sandblasted Surface G NPL G NPL
A ASTM A106 GR B A Hot Dip Galvanized per ASTM A153 H NPM H NPM
B ASTM A333 B Zinc Electroplated per ASTM B633 I ISO I ISO
- - C
A ASTM A106 GR B A Plain with Zinc Phosphate Coating
B ASTM A333 B Plain with Sandblasted Surface
A ASTM A106 GR B A Hot Dip Galvanized per ASTM A153
B ASTM A333 B Zinc Electroplated per ASTM B633
- - C
A ASTM A106 GR B A Plain with Zinc Phosphate Coating
B ASTM A333 B Plain with Sandblasted Surface
A ASTM A106 GR B A Hot Dip Galvanized per ASTM A153
B ASTM A333 B Zinc Electroplated per ASTM B633
- - C
A
ASTM A53, Type F, CW
B
ASTM A53, Type E, EW
A
ASTM A53, Type F, CW
ASTM A53, Type E, EW
B
- - C
A
ASTM A53, Type F, CW
B
ASTM A53, Type E, EW
A
ASTM A53, Type F, CW
B
ASTM A53, Type E, EW
- - C
A
ASTM A53, Type E, EW
A
ASTM A53, Type F, CW
B
ASTM A53, Type E, EW
ASTM A53, Type E, EW
A
A
ASTM B43 Brass
A
ASTM B43 Brass
Zinc Electroplated with Yellow Chromate
Zinc Electroplated with Yellow Chromate
Zinc Electroplated with Yellow Chromate
Zinc Electroplated with Yellow Chromate
A Plain with Zinc Phosphate Coating
B Plain with Sandblasted Surface
A Hot Dip Galvanized per ASTM A153
B Zinc Electroplated per ASTM B633
Zinc Electroplated with Yellow Chromate
A Plain with Zinc Phosphate Coating
B Plain with Sandblasted Surface
A Hot Dip Galvanized per ASTM A153
B Zinc Electroplated per ASTM B633
Zinc Electroplated with Yellow Chromate
A Plain with Zinc Phosphate Coating
B Plain with Sandblasted Surface
C Zinc Electroplated per ASTM B633
D
Zinc Electroplated with Yellow Chromate
A Plain with Zinc Phosphate Coating
B Plain with Sandblasted Surface
C Zinc Electroplated per ASTM B633
Zinc Electroplated with Yellow Chromate
D
A Plain with Zinc Phosphate Coating
B Plain with Sandblasted Surface
C Zinc Electroplated per ASTM B633
D
Zinc Electroplated with Yellow Chromate
A Plain
B Chrome Plated
A Plain
B Chrome Plated
1
⁄8
1
⁄4
3
⁄8
1
⁄2
3
⁄4
E ROE E ROE
1
1
1
⁄4
11⁄2
2
1
2
⁄2
3
J GRV J GRV
K LHT K LHT
4
5
6
End Codes
NPT
PLN
PSQ
PDB
ROE
BEV
NPL
NPM
ISO
GRV
LHT
Standard NPT Thread per
ASME B1.20.1 (RH) (TOE)
Plain End/Roller Cut
Plain End with Square or Saw Cut
Plain End with Square Cut
and Deburred
Ream One End - Square Cut
End with Ream
Square Cut End with 37
NPSL Straight Thread per ASME
B1.20.1 (Locknut) (Toe)
NPSM Straight Thread per ASME
B.1.20.1 (Mechanical) (Toe)
ISO/BSPT Taper Threads per ISO 7/1
Cut Grooved End per Anvil Specification
NPT-LH / Left Handed NPT Thread
per ASME B.1.20.1 (TOE)
Up to 24"
Maximum
Specify to the
nearest 1⁄16"
1
⁄2˚ Bevel
PF-11.16
Page 4
PIPE NIPPLES
Special Design Pipe Nipples
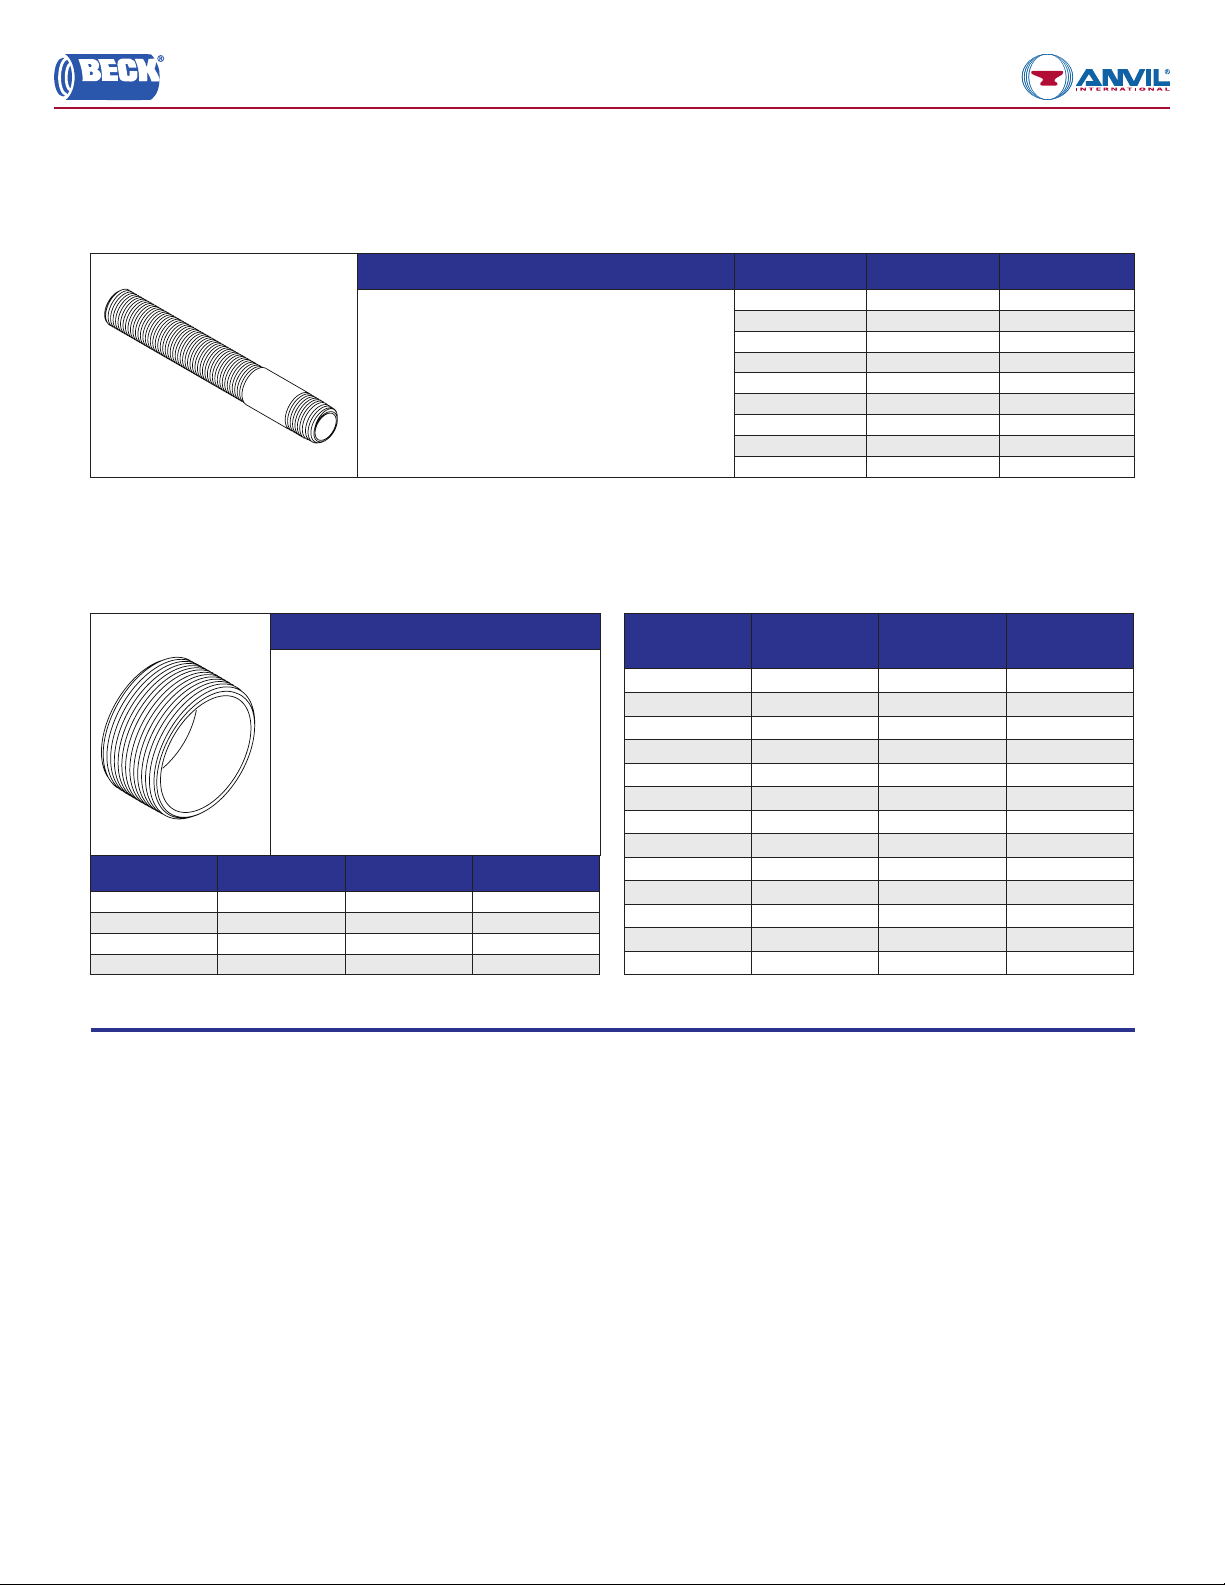
TANK NIPPLES
FIG. 341SD - Black & Galvanized
Description Size Length Weight
Tank Nipples are recommended for use as tank
legs, not intended for pressure service.
Tank Nipples have standard NPT threads on one
end and straight NPSM threads running for 4" on
the other end. Tank Nipples are fabricated from
ASTM A53 Schedule 40 welded pipe.
All Tank Nipples ship in quantities of 25.
Not intended for pressure service.
1
⁄8 6 0.13
1
⁄4 6 0.20
3
⁄8 6 0.28
1
⁄2 6 0.40
3
⁄4 6 0.53
1 6 0.76
1
⁄4 6 1.04
1
1
⁄2 6 1.28
1
2 6 1.56
BUTT NIPPLES
FIG. 344SD - Black & Galvanized
Description
RIGHT & LEFT NIPPLES
Black — Figure 339SD & Galvanized — Figure 343SD
Nom.
Pipe Size
Butt Nipples are intended for joining
couplings or female threaded components
end to end without exposing male threads.
Butt Nipples have standard NPT male
threads on both ends. Threads may have
fewer imperfect threads due to reduced
nipple length. Butt Nipples are fabricated
from ASTM A53 Schedule 40 welded pipe.
Size Length Weight Quantity
2 11⁄4 0.28 25
1
⁄2 2 0.87 10
2
3 2 1.28 10
4 2
1
⁄4 1.11 5
1
⁄8 4" or 6" 0.09 -
1
⁄4 4" or 6" 0.13 -
3
⁄8 4" or 6" 0.18 25
1
⁄2 4" or 6" 0.25 25
3
⁄4 4" or 6" 0.35 25
1 4" or 6" 0.51 25
1
⁄4 4" or 6" 0.68 25
1
1
⁄2 4" or 6" 0.80 25
1
2 4" or 6" 1.09 25
1
⁄2 4" or 6" 1.50 -
2
3 4" or 6" 2.00 -
1
⁄2 4" or 6" 2.80 -
3
4 4" or 6" 3.24 -
General Assembly of Threaded Fittings
1) Inspect both male and female components prior to assembly.
• Threads should be free from mechanical damage, dirt, chips and excess cutting oil.
• Clean or replace components as necessary.
Length Weight Quantity
2) Application of thread sealant
• Use a thread sealant that is fast drying, sets-up to a semi hard condition and is vibration resistant. Alternately, an anaerobic
sealant may be utilized.
• Thoroughly mix the thread sealant prior to application.
• Apply a thick even coat to the male threads only. Best application is achieved with a brush stiff enough to force sealant down
to the root of the threads.
3) Joint Makeup
• For sizes up to and including 2" pipe, wrench tight makeup is considered three full turns past handtight. Handtight engagement
for 1⁄2" through 2" thread varies from 41⁄2 turns to 5 turns.
• For 21⁄2" through 4" sizes, wrench tight makeup is considered two full turns past handtight. Handtight engagement for 21⁄2"
through 4" thread varies from 51⁄2 turns to 63⁄4 turns.
PF-11.16
 Loading...