

Page 1
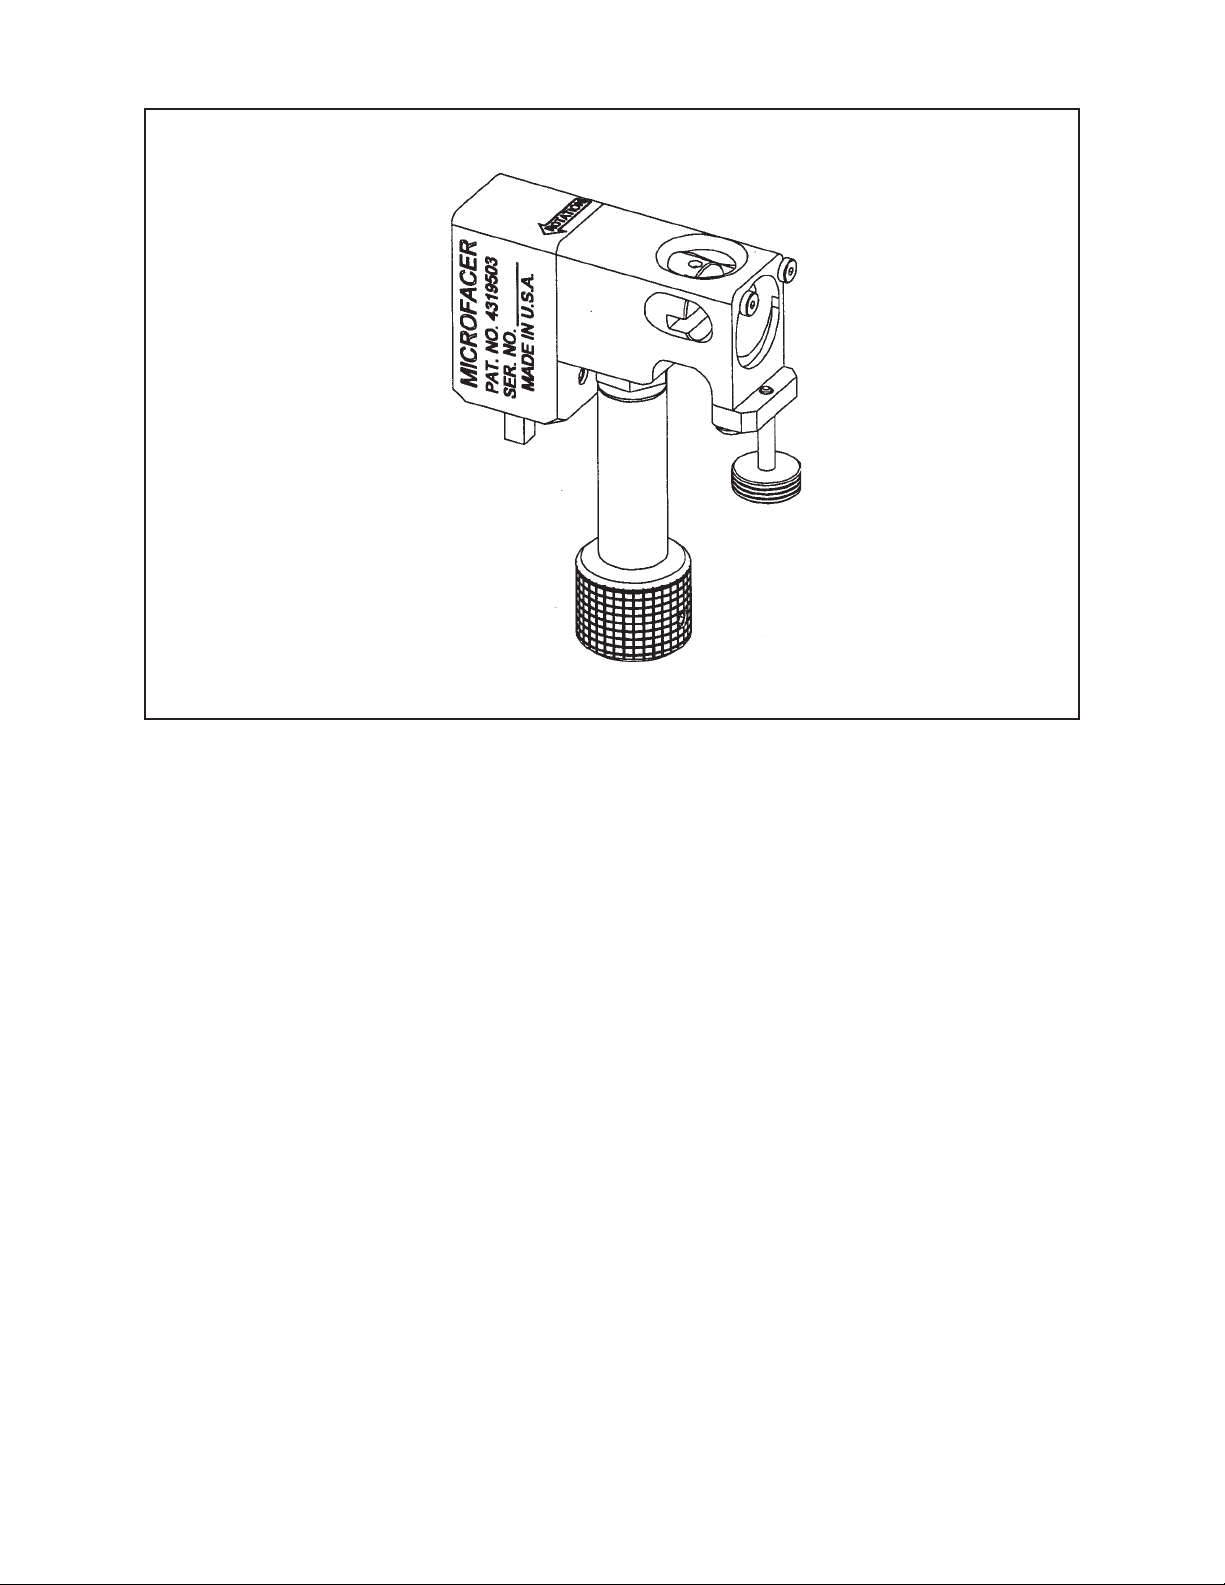
TABLE OF CONTENTS
CUSTOMER MESSAGE Inside Front Cover
SAFETY PRECAUTIONS 3
92-0756 Rev. 060811
Model 300 MICROFACER™
SPECIFICATIONS 6
MAINTENANCE 7
OPERATION 8
CUTTING SPEEDS AND FEEDS 10
SADDLE SETS 12
TOOL BITS 15
TROUBLE SHOOTING 16
ACCESSORIES 18
ILLUSTRATED PARTS BREAKDOWN 19
DEWALT SAFETY INSTRUCTIONS 23
TOOL BIT RESHARPENING POLICY Inside Back Cover
WARRANTY INFORMATION Inside Back Cover
Page 2
Copyright 2006
Proprietary property of TRI TOOL Inc.
No reproduction, use, or duplication of the information
shown hereon is permitted without the express written
consent of TRI TOOL Inc.
Page 3
SAFETY PRECAUTIONS
IN GENERAL
When using rotating head cutting equipment, basic safety precautions should always
be followed to reduce the risk of personal injury.
Operate this tool only in accordance with specific operating instructions.
Do not override the deadman switch on the power unit. Locking down, ob-
WARNING:
DRESS CONSIDERATIONS
structing, or in any way defeating the deadman switch on the power drive unit
may result in serious injury.
Model 300 MICROFACER™
Use standard safety equipment. Hard hats, safety shoes, safety harnesses, protective clothes, and other safety devices should always be used when appropriate.
Use safety glasses. Do not operate cutting tools without eye protection.
Dress properly. Do not wear loose clothing or jewelry. They can be caught in rotating and moving parts. Avoid slippery floors or wear nonskid footwear. If you have
long hair, wear protective hair covering to contain it.
WORK AREA
Keep the work area clean. Cluttered work areas and benches invite injuries.
Consider the work area environment. Keep the area well lit. Keep electrical cords,
cables, rags, rigging straps, and etc. clear of rotating equipment. Do not use powercutting tools in the presence of flammable liquids and gasses.
Keep visitors away. Do not let visitors or untrained personnel at or near operating
tools. Enforce eye protection requirements for all observers.
Do not over reach. Keep proper footing at all times.
Stay alert. Watch what you are doing. Use common sense. Do not operate tools
when you are tired.
92-0756 : Rev. 060811
3
Page 4
TRI TOOL INC.
TOOL CARE
Maintain tools with care. Keep tools in good operating condition. Sharp tool bits
perform better and safer than dull tool bits. Well maintained tools function properly
when needed.
Check for damaged parts. If a tool has malfunctioned, been dropped or hit, it must
be checked for damage. Run no-load tests and feed function checks. Do a complete visual inspection.
Electric motors. Use only with proper AC voltage power sources and observe all
normal electric shock hazard procedures.
Do not abuse power and control cords. Pulling or running over cords and cables
can result in electrical shock hazards and malfunctions. Keep control and power
cords out of all cutting fluids and water.
Hydraulic drives. Observe proper procedures for electrically driven power sources.
Avoid damage to hydraulic lines. Keep quick-disconnects clean. Grit contamination
causes malfunctions.
Air tools. Check the exhaust muffler. Broken or damaged mufflers can restrict air
flow or cause excessive noise. Use air motors only with a filtered, lubricated and
regulated air supply. Dirty air, low-pressure air or over pressure air will cause malfunctions, including delayed starting.
AREA EQUIPMENT
Secure work. Whenever possible use clamps, vises, chains and straps to secure
pipe.
Make sure the tool is secured; it is safer to have both hands free to operate the tool.
TOOL USE
Use the right tool and tool bit for the job. Do not use a tool, which is incorrect for the
job you are doing.
Keep the tool bits fully engaged in the tool bit holders. Loose bits are a safety hazard.
4
92-0756 : Rev. 060811
Page 5
Model 300 MICROFACER™
Disconnect power supply during setup and maintenance. Use all ‘Stop’ or Shut off’
features available when changing or adjusting tool bits, maintaining the tool, or when
the tool is not in use.
Remove adjusting keys and wrenches before applying power to the equipment.
Develop a habit of checking the tool before turning it on to make sure that all keys
and wrenches have been removed.
Do not force tools. Tools and tool bits function better and safer when used at the
feed and speed rate for which they were designed.
Do not reach into rotating equipment. Do not reach into the rotating head stock to
clear chips, to make adjustments, or to check surface finish. A machine designed to
cut steel will not stop for a hand or an arm.
Handle chips with care. Chips have very sharp edges and are hot. Do not try to pull
chips apart with are hands; they are very tough.
Avoid unintentional starts. Do not carry or handle tools with your hand on the operating switches or levers. Do not lay the tool down in a manner that will start the
drive. Do not allow the tool to flip around or move when adjusting or changing tool
bits.
Store idle tools properly. Disconnect tools from the power source and store in a safe
place. Remove tool bits for safe handling of the tool.
92-0756 : Rev. 060811
5
Page 6
TRI TOOL INC.
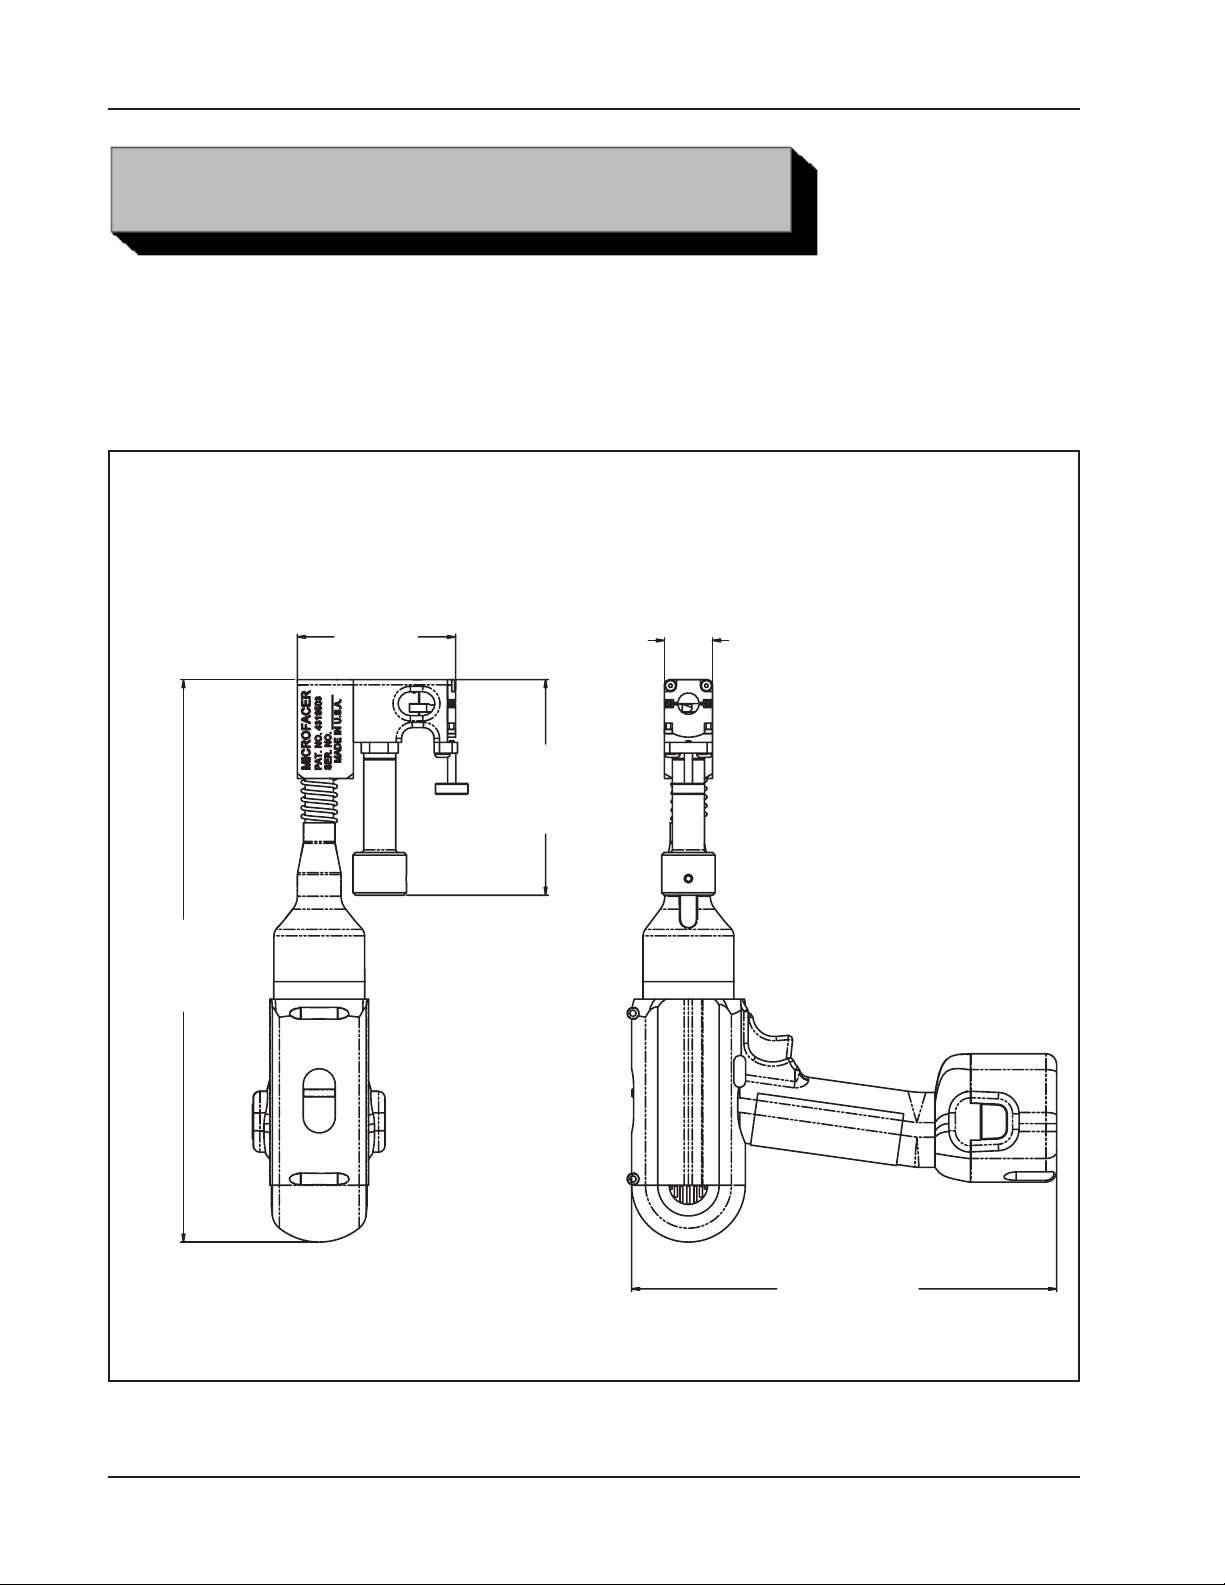
The Model 300 MICROFACER™Tube Squaring Tool has been developed to square
the ends of up to .75” (19.0 mm) OD tubing.
Weight: 5.35” (2.4 Kg)
Envelope Drawing
SPECIFICATIONS
1.13"
(28.6 mm)
3.70"
(94.0 mm)
13.15"
(334.1 mm)
5.04"
(128.0 mm)
9.94"
(252.5 mm)
6
92-0756 : Rev. 060811
Page 7
Model 300 MICROFACER™
MAINTENANCE
All components should be cleaned and coated with a light film of oil prior to use.
Use a clean, non-detergent oil, preferably SAE 10 (90 SSU) or lighter.
When the Model 300 is operated in the vertical position, cutting head up, it should
be turned upside down and the chips and/or other debris removed after each tube
squaring operation has been completed.
Tool life may be severely shortened, unless chips and/or other debris that
NOTE:
have been deposited on the cutting head during the machining operation are
removed.
92-0756 : Rev. 060811
7
Page 8
TRI TOOL INC.
OPERATION
Read the Operating Instructions carefully before attempting to operate the Model
300 MIROFACER™Tube Squaring Tool.
Use eye protection at all times when operating Model 300.
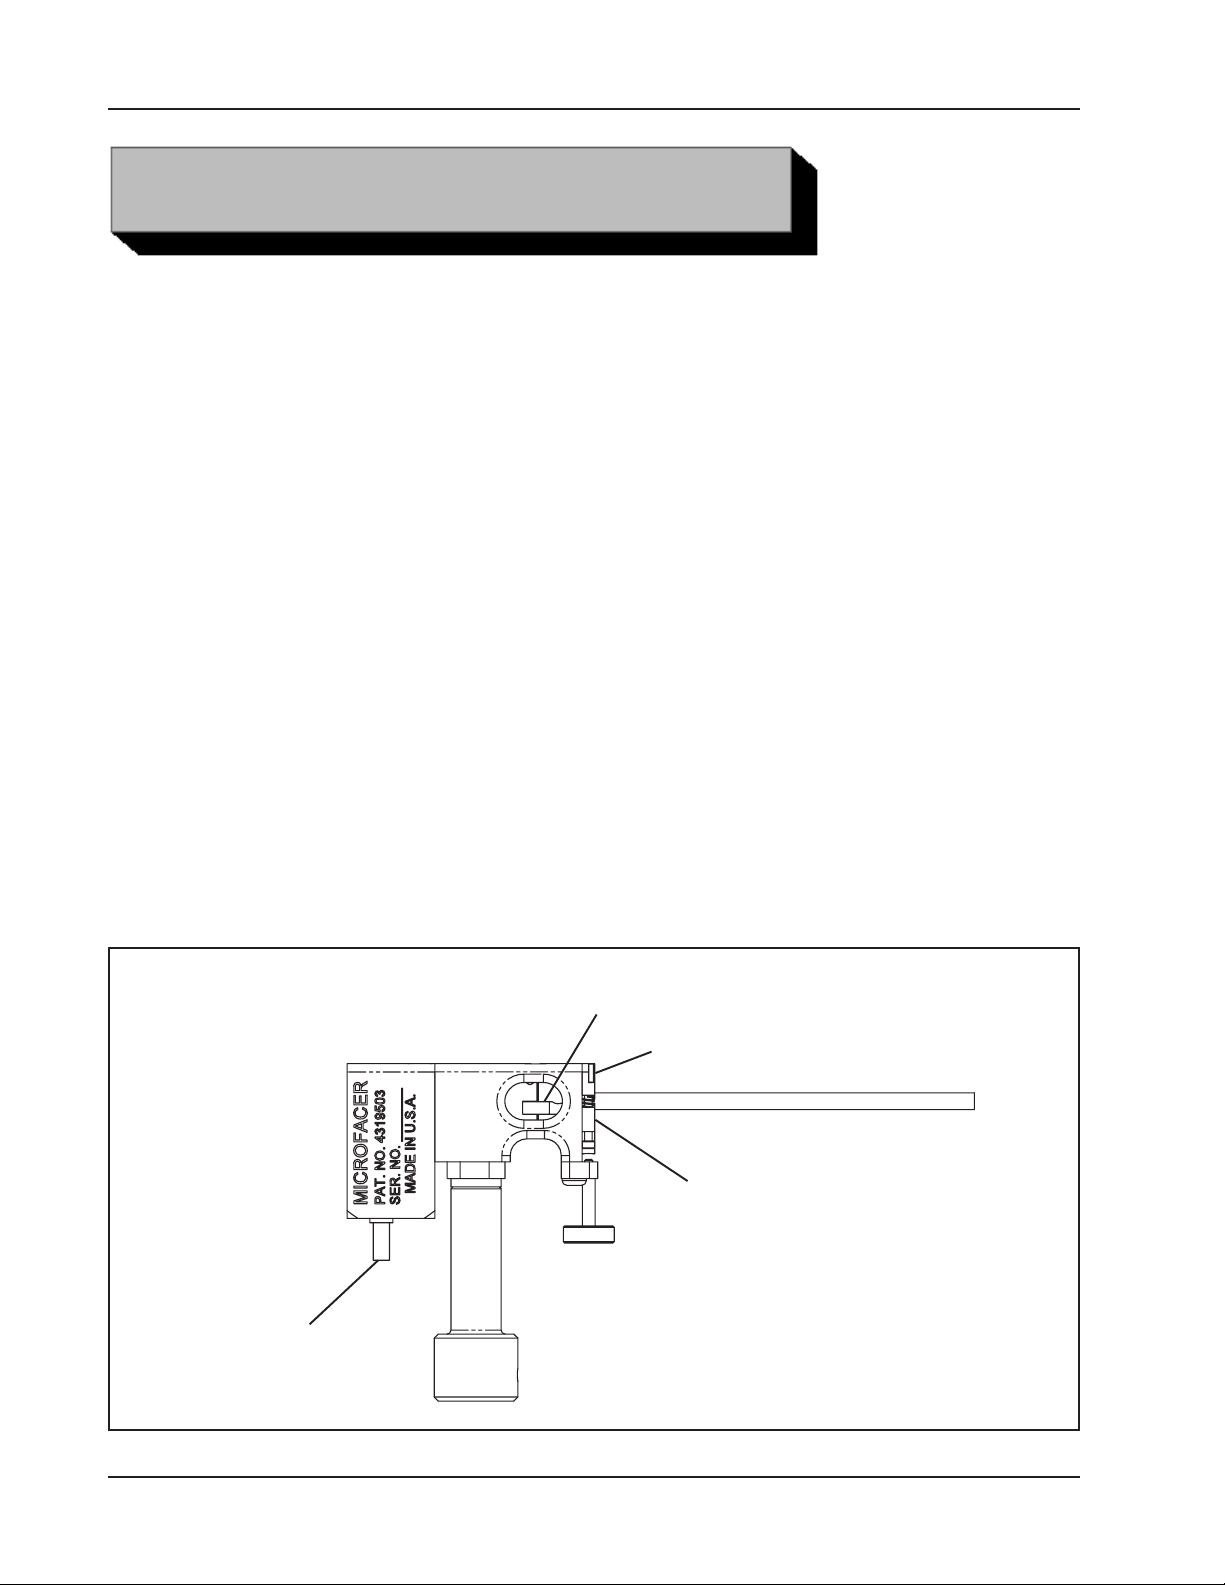
INSTALLING THE SADDLE SET
Select the saddle set which is the proper size for the OD of the tube which is to be
machined.
Squeeze the saddle set to compress the springs and insert the saddle set into the
front of the Model 300.
Retain the saddle set by inserting the two (2) cap screws into the front of the saddle
set.
INSTALLING THE TOOL BIT
Select the tool bit to be installed.
Slide the tool bit into the slot on front of the main shaft.
Tool Bit
Cap Screws
Saddle Set
Drive Line
Shank
8
92-0756 : Rev. 060811
Page 9
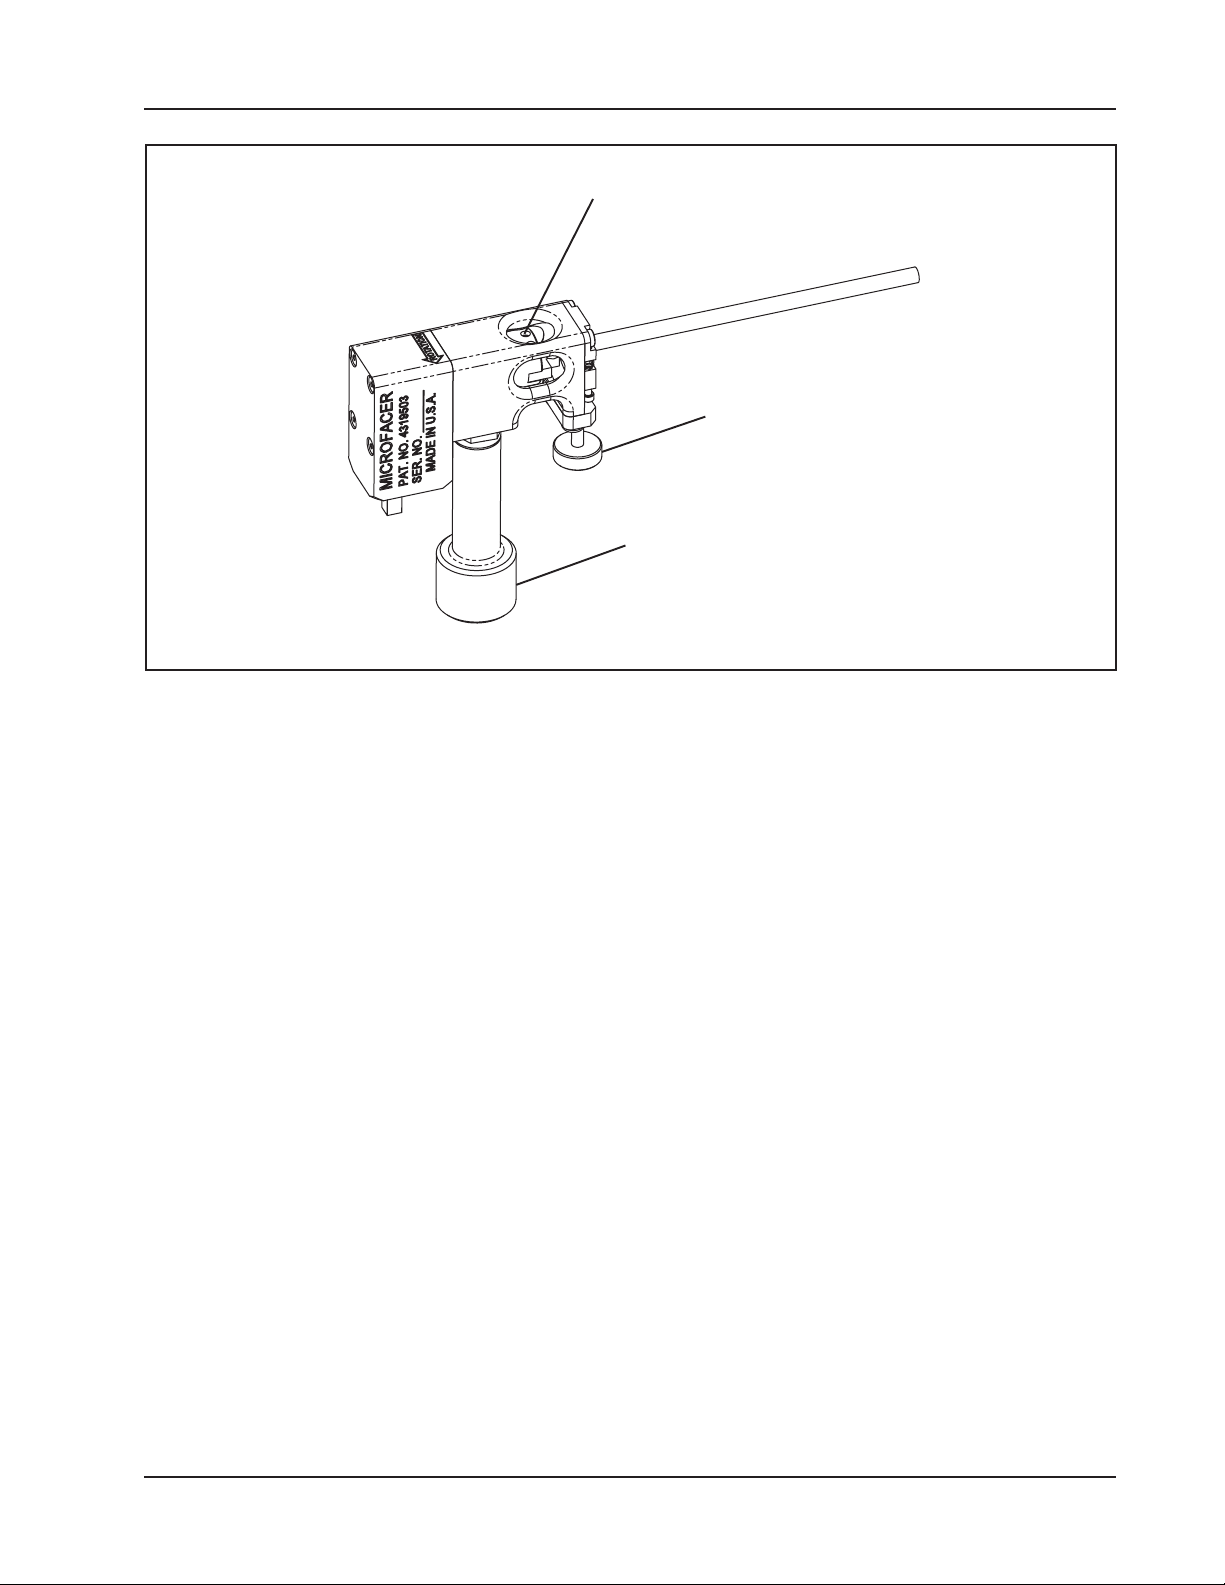
Set Screws
(Retaining
Tool Bit)
Feed Knob
Model 300 MICROFACER™
Clamp Knob
INSTALLATION
Slide the tube to be worked on into the saddle, leaving approximately 1/8” (3 mm)
between the tool bit and the end of the tube.
INSERT IMAGE
Tighten the saddle set by turning the clamp knob below the saddle set.
MACHINING SEQUENCE
Turn the motor on and let it slowly rotate to ensure that the tool bit does not make
contact with the end of the tube at this time.
Loosen the clamp knob to release the saddle set and remove the machined tube.
92-0756 : Rev. 060811
9
Page 10
TRI TOOL INC.
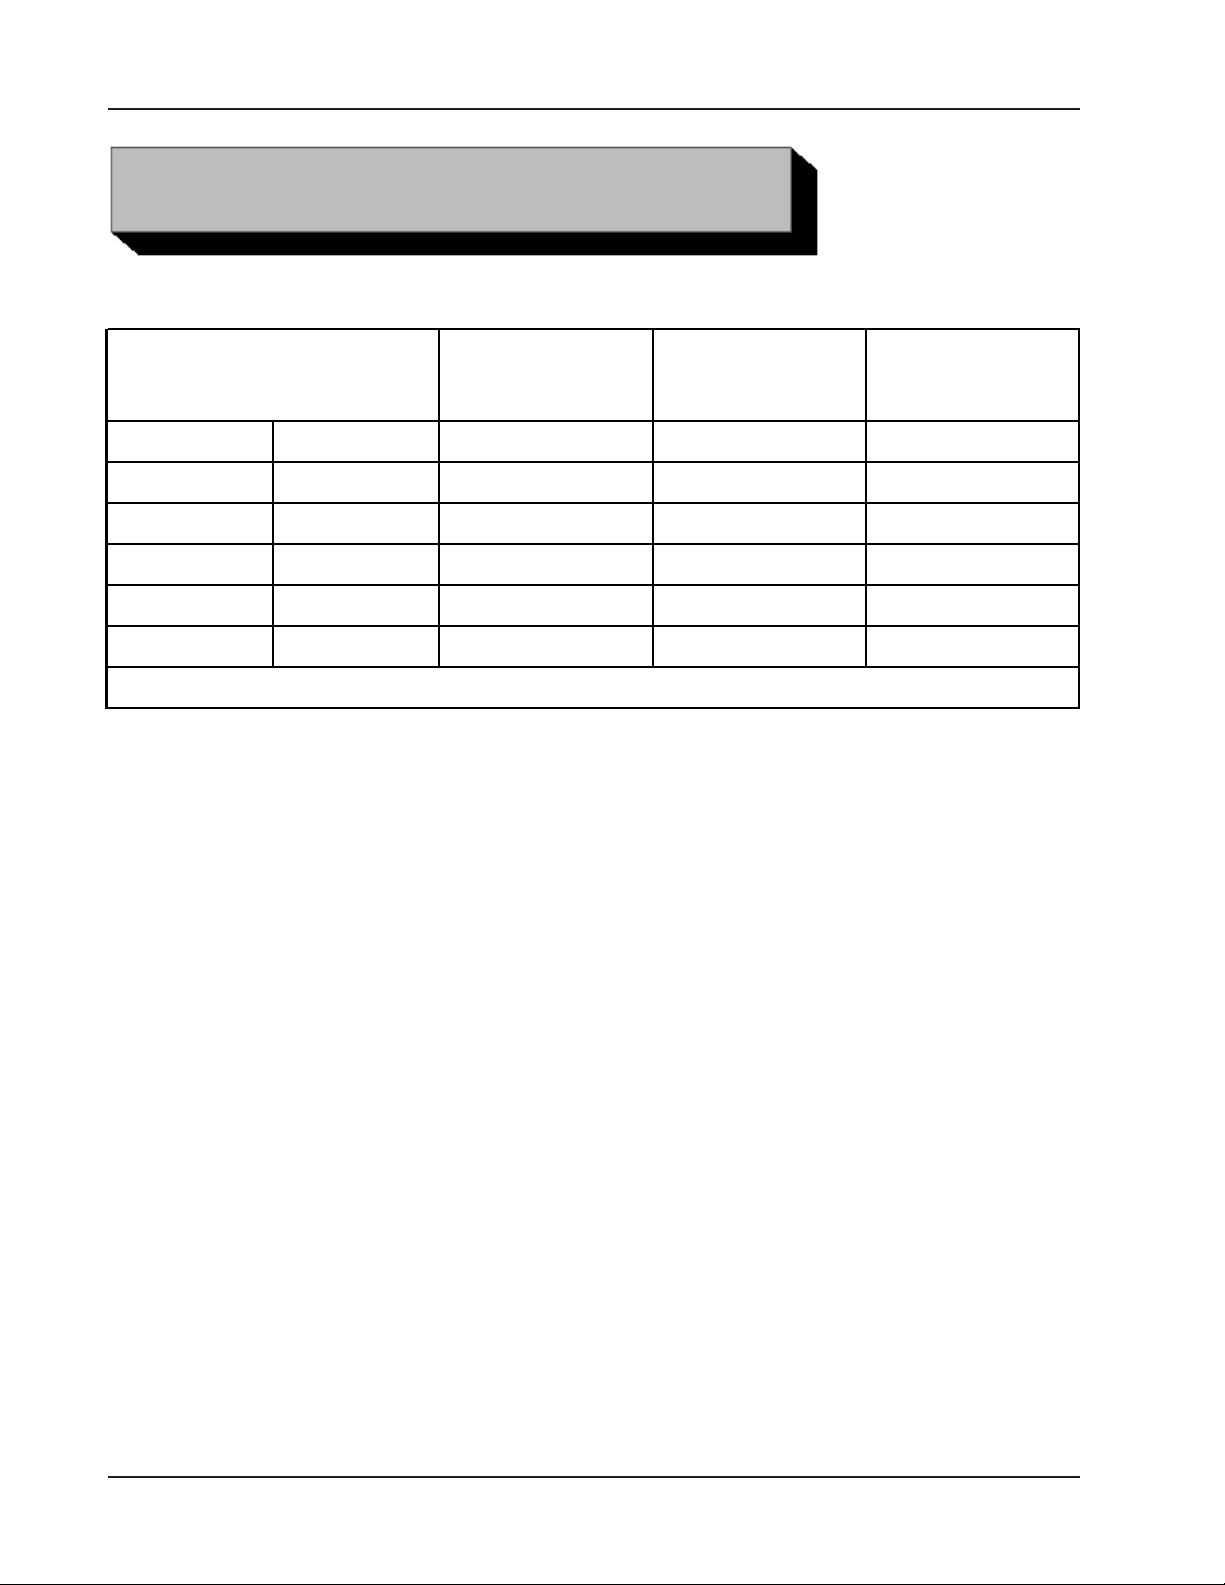
CUTTING SPEEDS AND FEEDS
RPM for
True DIA
.125" 3.18 mm 509 636 763
.250" 6.35 mm 255 318 382
.375 9.53 mm 170 212 255
.500" 12.70 mm 127 159 191
.625" 15.88 mm 102 127 153
.750" 19.05 mm 85 106 127
Cutting Speed (Approximately)
200 in/min
(5080 mm/min)
RPM for
250 in/min
(6350 mm/min)
Use 200 surface inches per minute (5080 surface millimeters per minute) for:
Stainless steels in general when no coolant is allowed, all heavy-wall tube
and some chrome/molybdenum steels.
RPM for
300 in/min
(7620 mm/min)
Use 250 surface inches per minute (6350 surface millimeters per minute) for:
Mild steels and some thin-wall stainless steels when coolants are permitted
and applied.
Use 300 surface inches per minute (7620 surface millimeters per minute) for:
Aluminum and some thin-wall mild steel and tube with coolants.
BASIC FEED RECOMMENDATION
Use very light feed for initial beveling or until a continuous cut is established.
This is very important for longer tool bit life when cutting through flame cut or out of
square pipe ends.
10
92-0756 : Rev. 060811
Page 11
Model 300 MICROFACER™
Use adequate feed, .003” to .006” (.08mm to .15mm) per revolution thereafter, to
establish a continuous chip cut.
If the feed is too light, only light stringer chips will be removed.
If the feed is too heavy the drive will start to overload and the chip will start to
have a rough or torn appearance.
92-0756 : Rev. 060811
11
Page 12
TRI TOOL INC.
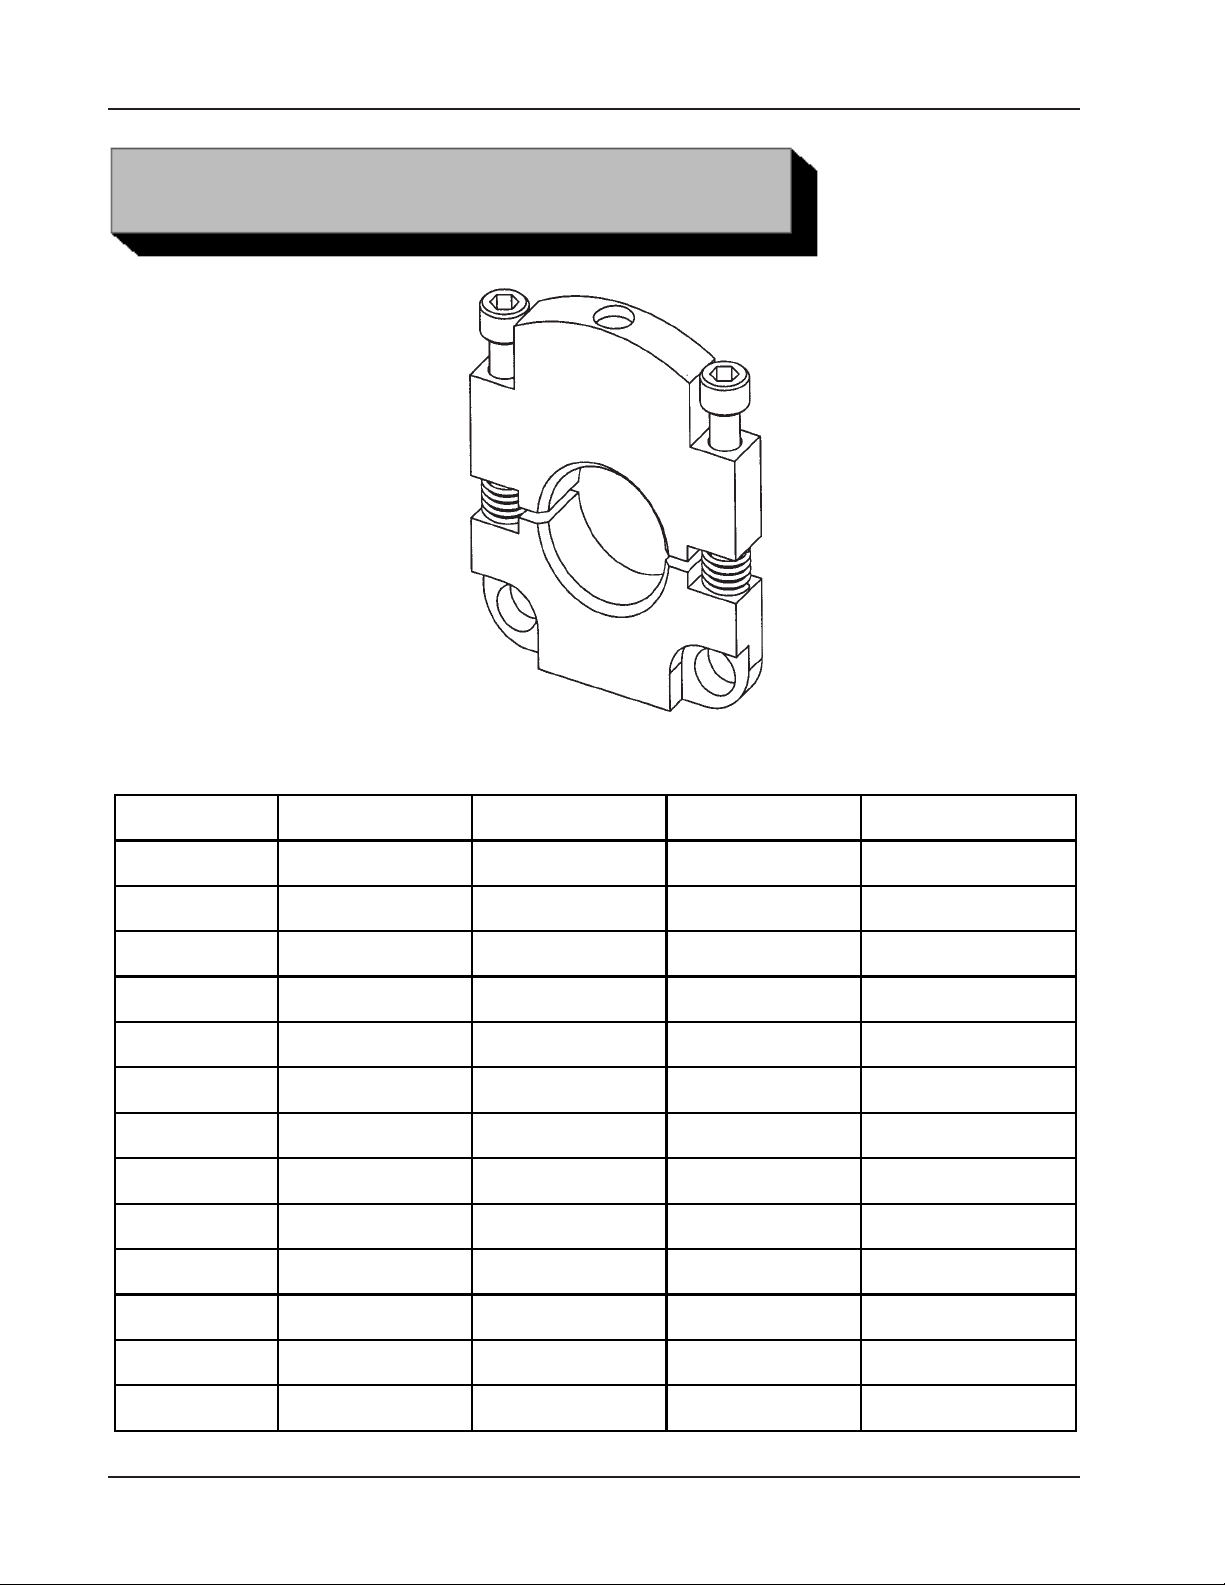
SADDLE SETS
Pipe Size Fraction Decimal Metric Saddle P/N
1/8" .125" 3.18 mm 67-4193
5/32" .156" 3.96 mm 67-4194
.158" 4.00 mm 67-4195
3/16" .188" 4.76 mm 67-4196
.197" 5.00 mm 67-4197
7/32" .219" 5.56 mm 67-4198
.234" 5.95 mm 67-4199
.236" 6.00 mm 67-4200
1/4" .250" 6.35 mm 67-4201
.276" 7.00 mm 67-4202
9/32" .281" 7.14 mm 67-4203
.283" 7.20 mm 67-4204
12
5/16" .313" 7.95 mm 67-4205
92-0756 : Rev. 060811
Page 13
Model 300 MICROFACER™
Pipe Size Fraction Decimal Metric Saddle P/N
.315" 8.00 mm 67-4206
11/32" .344" 8.74 mm 67-4207
.354" 9.00 mm 67-4208
.359" 9.13 mm 67-4209
3/8" .375" 9.53 mm 67-4210
.394" 10.00 mm 67-4211
.400" 10.16 mm 67-4212
1/8" 13/32" .406" 10.31 mm 67-4213
.413" 10.50 mm 67-4214
.422" 10.72 mm 67-4215
.433" 11.00 mm 67-4216
7/16" .438" 11.13 mm 67-4217
15.32" .469" 11.91 mm 67-4218
.472" 12.00 mm 67-4219
1/2" .500" 12.70 mm 67-4220
.512" 13.00 mm 67-4221
.531" 13.50 mm 67-4222
.535" 13.60 mm 67-4223
1/4" .540" 13.72 mm 67-4224
.543" 13.80 mm 67-4225
.547" 13.89 mm 67-4226
.551" 14.00 mm 67-4227
9/16" .563" 14.30 mm 67-4228
.591" 15.00 mm 67-4229
5/8" .625" 15.88 mm 67-4232
92-0756 : Rev. 060811
.594" 15.08 mm 67-4230
.602" 15.29 mm 67-4231
13
Page 14
TRI TOOL INC.
Pipe Size Fraction Decimal Metric Saddle P/N
.630" 16.00 mm 67-4233
.641" 16.27 mm 67-4234
.656" 16.66 mm 67-4235
.669" 17.00 mm 67-4236
3/8" .675" 17.15 mm 67-4237
.677" 17.20 mm 67-4238
.681" 17.30 mm 67-4239
11/16" .688" 17.48 mm 67-4240
.709" 18.00 mm 67-4241
.718" 18.24 mm 67-4242
3/4" .750" 19.05 mm 67-4243
14
92-0756 : Rev. 060811
Page 15
TOOL BITS
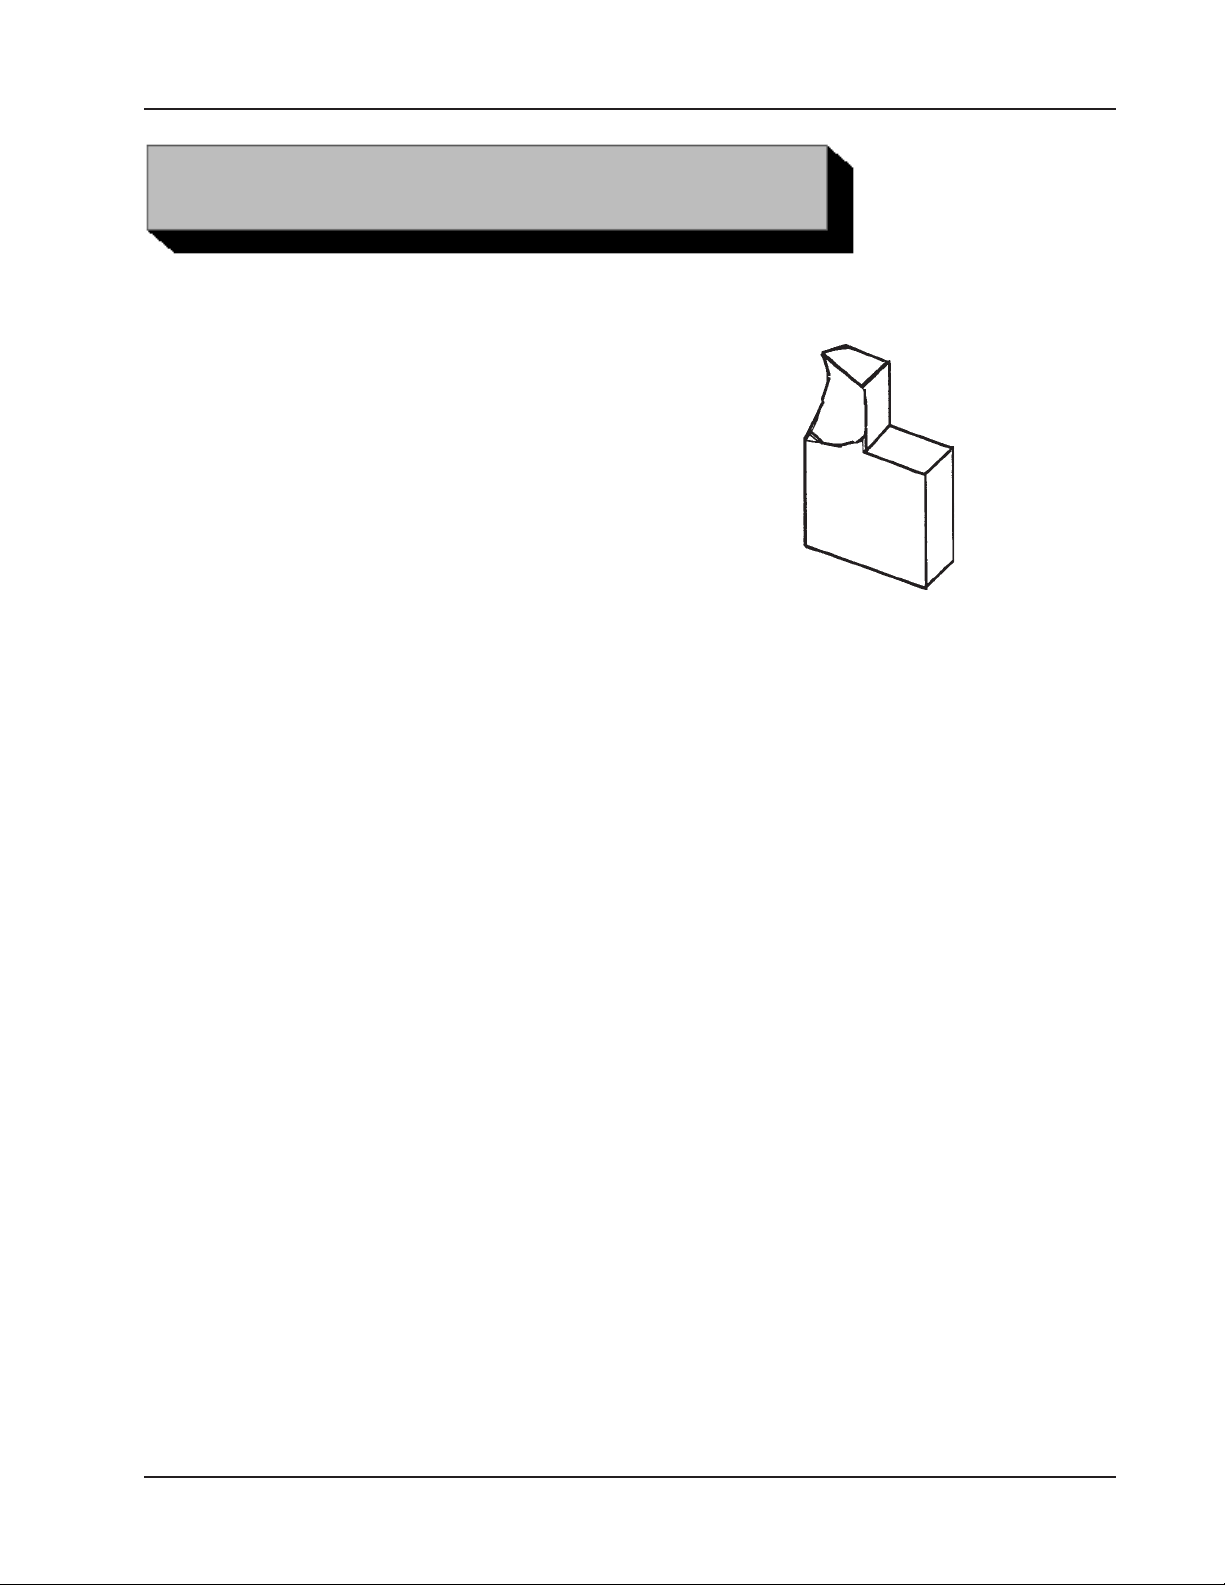
Tool Bit, Tube Squaring, P/N 99-0591
Model 300 MICROFACER™
92-0756 : Rev. 060811
15
Page 16
TRI TOOL INC.
TROUBLE SHOOTING
Problem: The Tool Bit Chatters
The tool bit is loose or overextended.
The tool bit is damaged.
The tool holder is too loose in the slides.
The cutting speed is too fast.
The clamping pads are loose on the pipe or tube.
Cutting fluid is required.
The main bearing pre-load is loose.
Problem: There is excessive Tool Bit wear
The pipe or tube material is too hard or abrasive.
The cutting speed is too fast.
Cutting fluid is required.
A dull Tool Bit is causing surface hardening conditions (Stainless pipe or
tubing).
There is scale or other foreign matter on the pipe or tube, which is dulling the
tool bit at the start of the cut.
The tool bit is incorrect for the material being cut.
Problem: The surface finish is rough
The tool bit is dull, chipped, etc.
Metal build-up on the cutting edge of the tool bit is creating a false cutting
edge.
Cutting fluid is required.
Problem: There is a loss of air power
16
The air supply pressure is too low.
The air filter is plugged.
The air line size is insufficient.
The air line is too long.
92-0756 : Rev. 060811
Page 17
Problem: The tool bit will not reach the work
Incorrect tool blocks are installed for the size of the pipe or tube being
worked on.
Incorrect tool bit is installed.
Model 300 MICROFACER™
92-0756 : Rev. 060811
17
Page 18
TRI TOOL INC.
The following accessories are recommended for use with the Model 300
MICROFACER and are available from TRI TOOL INC.
1. Flexable Shaft Assembly (18") - P/N 14-0036
2. Spare Battery, 9.6V - P/N 30-3131
3. Charger, 220V, 7.2V - 18V Dewalt - P/N 30-2614
4. Charger, 110V, 7.2V - 18V Dewalt - P/N 30-2615
A Filter/Regulator/Lubricator (FRL) is required to protect the warranty on all TRI
TOOL INC. air driven tools.
ACCESSORIES
18
92-0756 : Rev. 060811
Page 19
Model 300 MICROFACER™
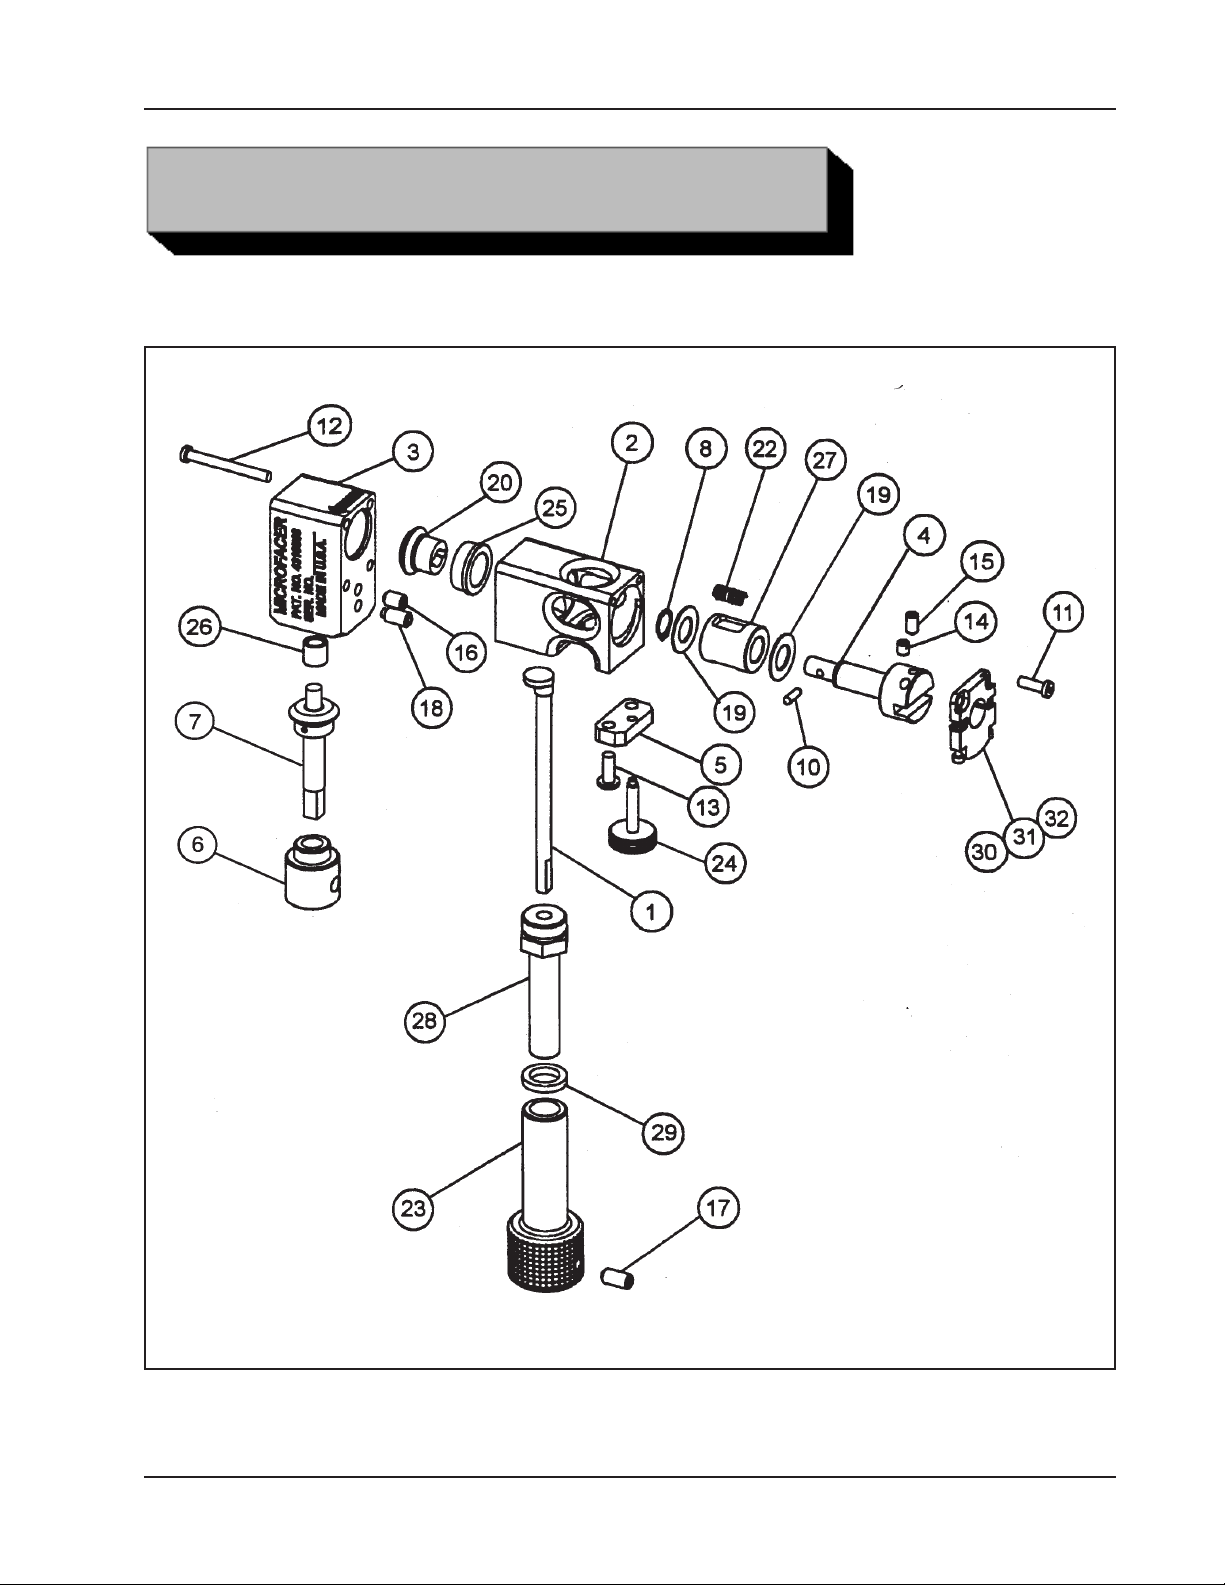
ILLUSTRATED PARTS BREAKDOWN
MODEL 300 MICROFACER™ BODY ASSEMBLY (P/N 02-2297)
92-0756 : Rev. 060811
19
Page 20
TRI TOOL INC.
Parts List, Model 300 MICROFACER™ Body Assembly (P/N 02-2297)
Item Part
No. No. Description Qty
1. 14-0006 SHAFT ASSEMBLY 1
2. 19-0838 HOUSING, MAIN 1
3. 19-0796 HOUSING, DRIVE 1
4. 20-0718 SHAFT, MAIN 1
5. 24-1614 PLATE, CLAMP 1
6. 27-0584 ADAPTER, DRIVE BUSHING 1
7. 27-0725 ADAPTER ASSEMBLY, CABLE DRIVE 1
8. 30-0302 RING, RETAINING, EXTERNAL 1
10. 32-0514 PIN, DRIVE, 1/8" DIA 1
11. 33-2110 SCREW, CAP, #8-32 X 1/2" 2
12. 33-2121 SCREW, CAP, #8-32 X 1 1/2" 4
13. 33-2112 SCREW, BUTTON, #10-24 X 1/2" 2
14. 33-0488 SET SCREW, CUP PT, #10-24 X 1/4" 2
15. 33-0490 SET SCREW, CUP PT., #10-24 X 3/8" 1
16. 33-0501 SET SCREW, CUP PT., 1/4-20 X 3/8" 1
17. 33-0503 SET SCREW, CUP PT., 1/4-20 X 1/2" 1
18. 33-0927 SET SCREW, HALF DOG, 1/4-20 X 1/2" 1
19. 34-0351 WASHER, THRUST 2
20. 39-0828 GEAR, BEVEL, MAIN 1
22. 40-0236 SPRING, COMPRESSION 1
23. 42-0174 HANDLE 1
24. 42-0175 KNOB, SADDLE ADJUST 1
25. 45-0306 BUSHING, MAIN 1
26. 45-0296 BUSHING, BRONZE
27. 46-0462 SLEEVE, MAIN 1
28. 46-0479 SLEEVE 1
29. 34-0060 WASHER 1
30. 67-XXXX SADDLE SET REF.
31. 33-2109 SCREW, CAP, #4-40 X 7/8" REF.
32. 40-0236 SPRING, COMPRESSION REF.
20
92-0756 : Rev. 060811
Page 21
Model 300 MICROFACER™
Parts List, Model 300 MICROFACER™ Body Assembly (P/N 02-2297) Con't.
Item Part
No. No. Description Qty
NOT SHOWN
36-0002 WRENCH, L, 5/64" HEX 1
36-0003 WRENCH, L, 3/32" HEX 1
36-0016 WRENCH, T, 3/32" HEX 1
92-0756 : Rev. 060811
21
Page 22
TRI TOOL INC.
4
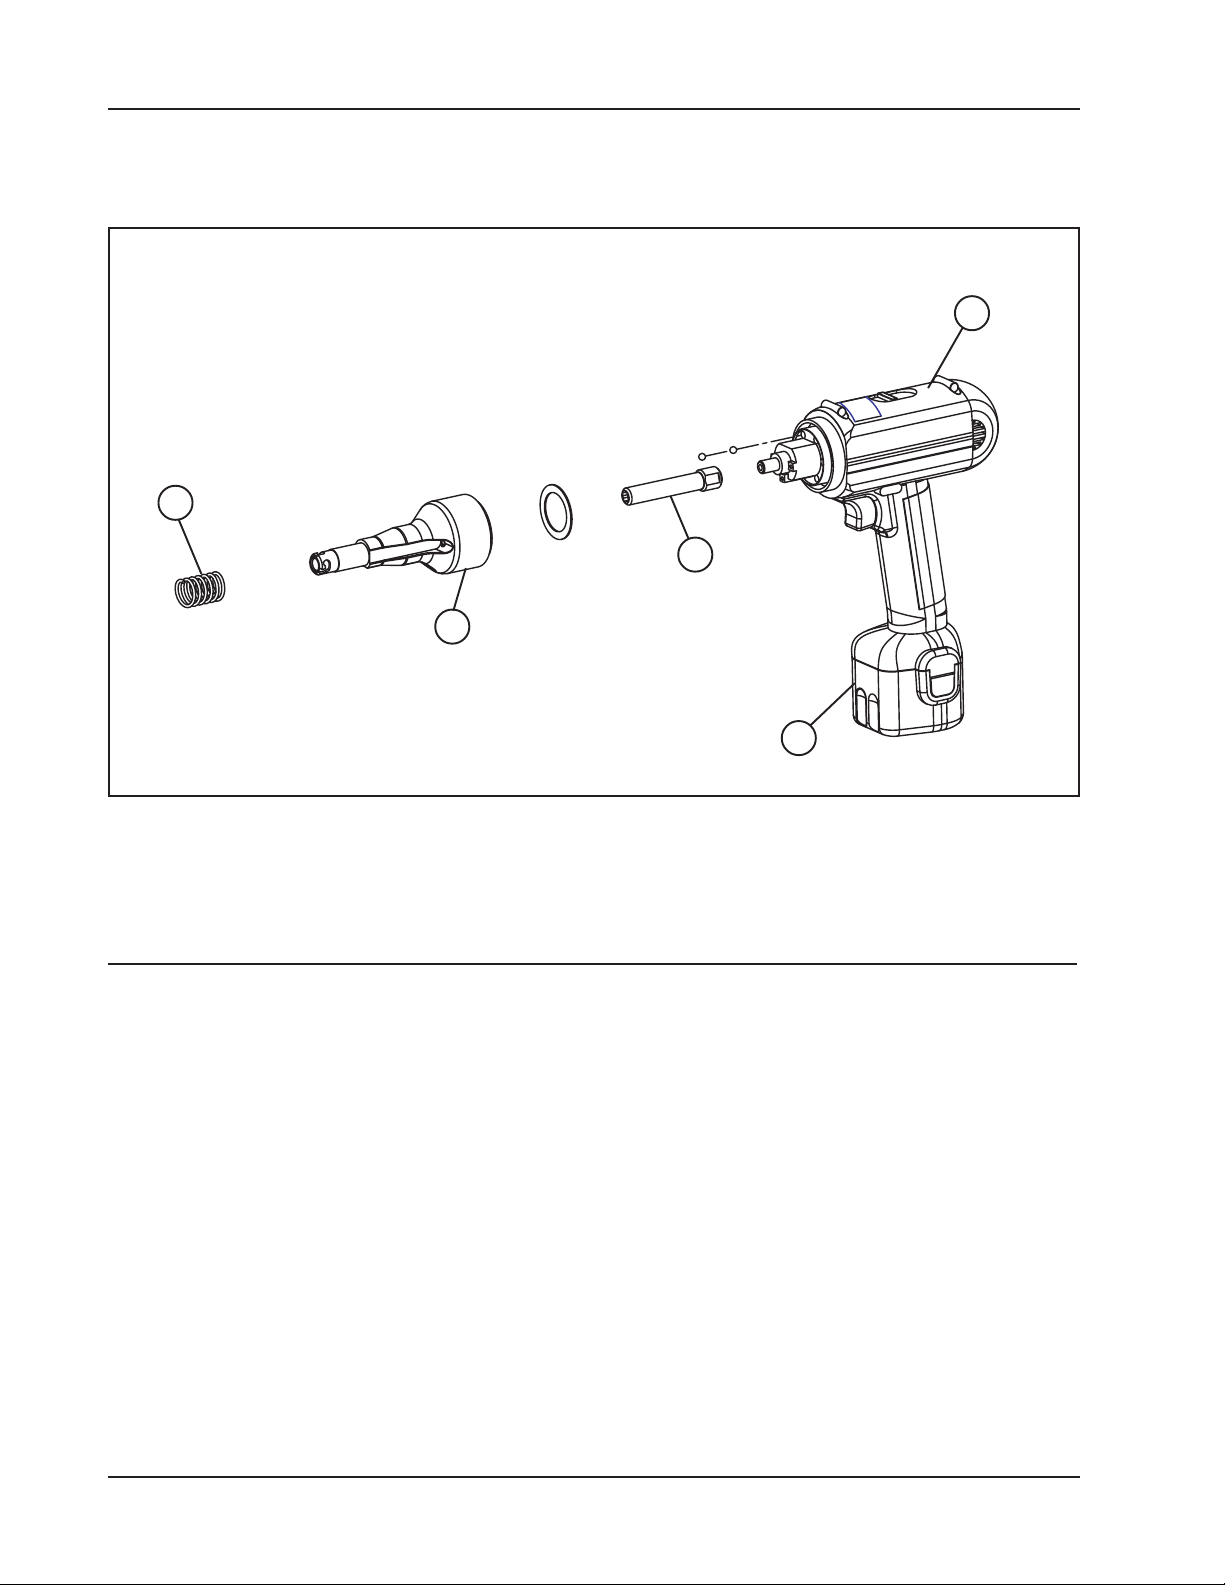
300MF MOTOR ASSEMBLY (P/N 58-0164)
5
1
2
3
Parts List, 300MF Motor Assemlby (P/N 58-0164)
Item Part
No. No. Description Qty
1. 20-0911 SHAFT, DRIVE 1
2. 27-0818 ADAPTER, BAYONET 1
3. 30-3131 BATTERY, 9.6V 1
4. 40-0143 SPRING, MUSIC WIRE, LC-085K-3 1
5. 58-0193 MOTOR, ELECTRIC, 9.6V, MOD. 1
22
92-0756 : Rev. 060811
Page 23
Model 300 MICROFACER™
DEWALT SAFETY INSTRUCTIONS
The DeWALT Cordless Drill/Driver comes with an 'Instruction Manual' and should be
referenced for all safety and operating procedures.
92-0756 : Rev. 060811
23
 Loading...