

Page 1
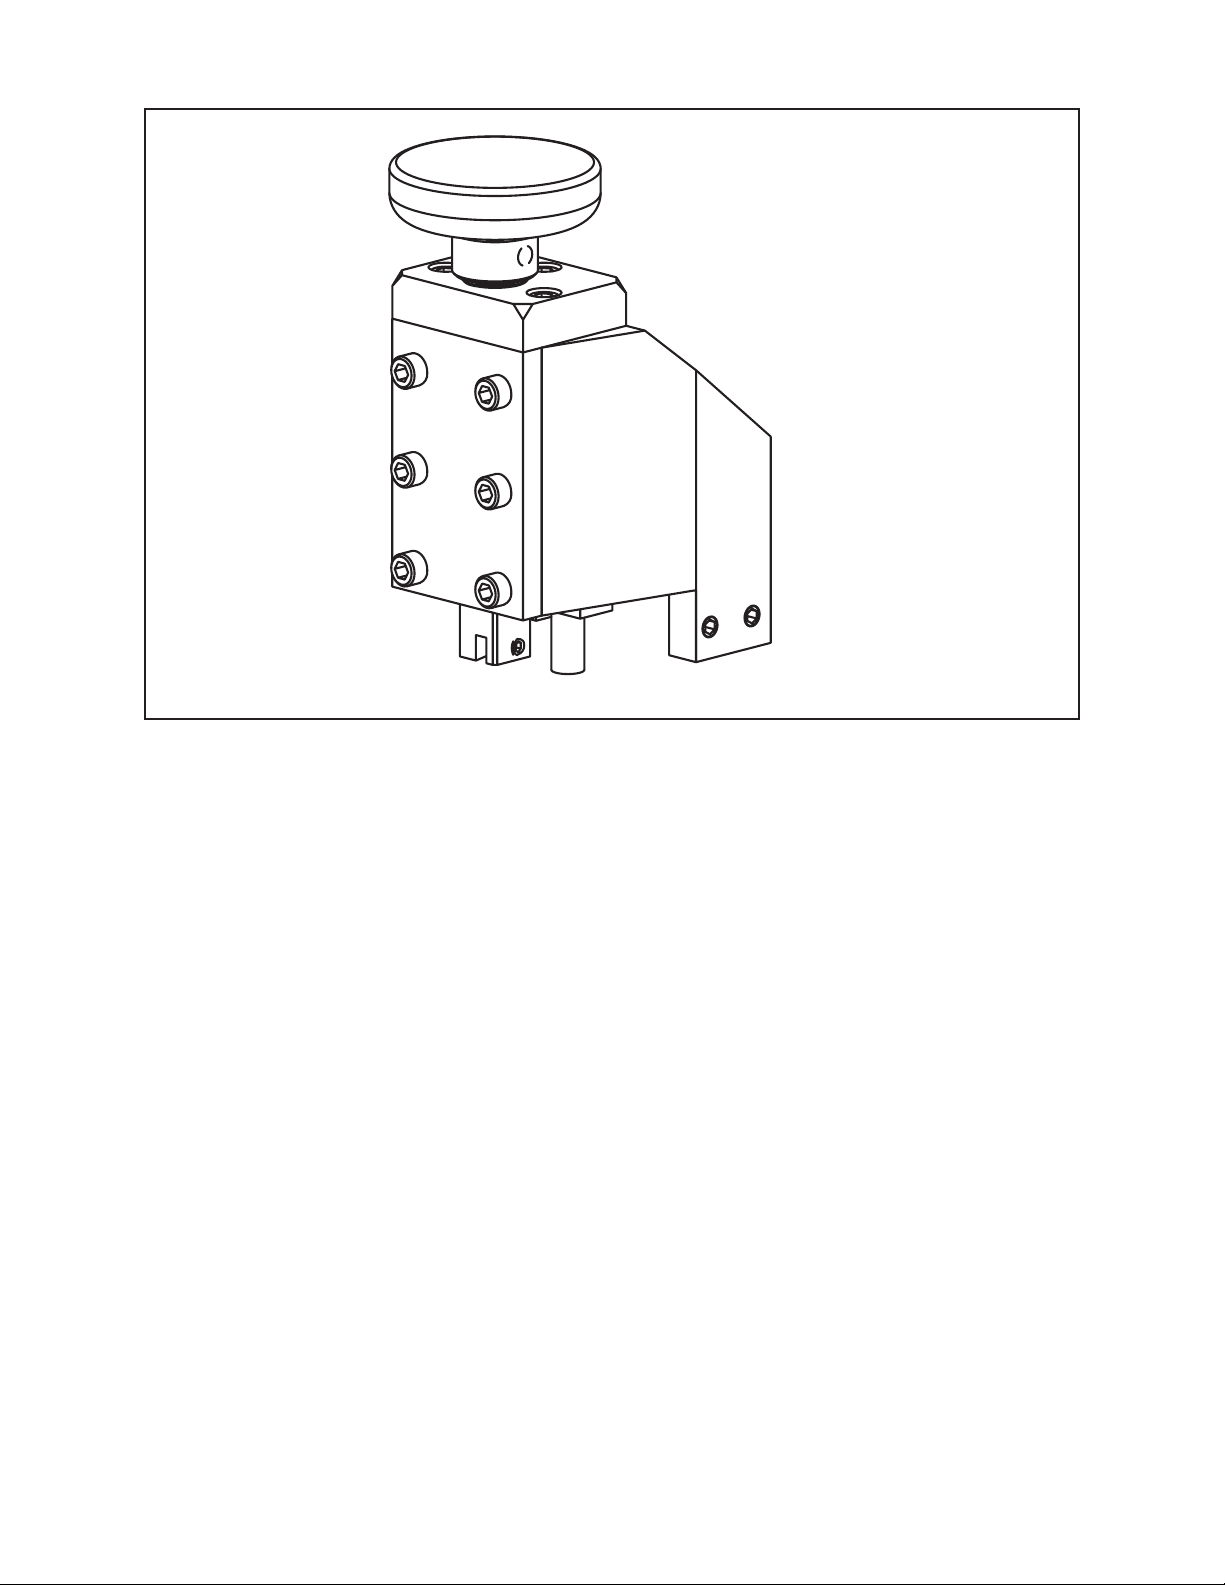
TABLE OF CONTENTS
CUSTOMER MESSAGE Inside Front Cover
SAFETY PRECAUTIONS 3
92-0192 Rev. 930618
Model CBM-1 Counterboring Module
GENERAL DESCRIPTION 6
SPECIFICATIONS 7
MAINTENANCE 9
OPERATION 10
CUTTING SPEEDS 12
TOOL BITS 13
TROUBLE SHOOTING 14
ILLUSTRATED PARTS BREAKDOWN 16
TOOL BIT RESHARPENING POLICY Inside Back Cover
WARRANTY INFORMATION Inside Back Cover
Page 2
Copyright 2005
Proprietary property of TRI TOOL Inc.
No reproduction, use, or duplication of the information
shown hereon is permitted without the express written
consent of TRI TOOL Inc.
Page 3
SAFETY PRECAUTIONS
IN GENERAL
When using rotating head cutting equipment, basic safety precautions should always
be followed to reduce the risk of personal injury.
Operate this tool only in accordance with specific operating instructions.
Do not override the deadman switch on the power unit. Locking down, ob-
WARNING:
DRESS CONSIDERATIONS
structing, or in any way defeating the deadman switch on the power drive unit
may result in serious injury.
Model CBM-1 Counterboring Module
Use standard safety equipment. Hard hats, safety shoes, safety harnesses, protective clothes, and other safety devices should always be used when appropriate.
Use safety glasses. Do not operate cutting tools without eye protection.
Dress properly. Do not wear loose clothing or jewelry. They can be caught in rotating and moving parts. Avoid slippery floors or wear nonskid footwear. If you have
long hair, wear protective hair covering to contain it.
WORK AREA
Keep the work area clean. Cluttered work areas and benches invite injuries.
Consider the work area environment. Keep the area well lit. Keep electrical cords,
cables, rags, rigging straps, and etc. clear of rotating equipment. Do not use powercutting tools in the presence of flammable liquids and gasses.
Keep visitors away. Do not let visitors or untrained personnel at or near operating
tools. Enforce eye protection requirements for all observers.
Do not over reach. Keep proper footing at all times.
Stay alert. Watch what you are doing. Use common sense. Do not operate tools
when you are tired.
92-0192 : Rev. 930618
3
Page 4
TRI TOOL INC.
TOOL CARE
Maintain tools with care. Keep tools in good operating condition. Sharp tool bits
perform better and safer than dull tool bits. Well maintained tools function properly
when needed.
Check for damaged parts. If a tool has malfunctioned, been dropped or hit, it must
be checked for damage. Run no-load tests and feed function checks. Do a complete visual inspection.
Electric motors. Use only with proper AC voltage power sources and observe all
normal electric shock hazard procedures.
Do not abuse power and control cords. Pulling or running over cords and cables
can result in electrical shock hazards and malfunctions. Keep control and power
cords out of all cutting fluids and water.
Hydraulic drives. Observe proper procedures for electrically driven power sources.
Avoid damage to hydraulic lines. Keep quick-disconnects clean. Grit contamination
causes malfunctions.
Air tools. Check the exhaust muffler. Broken or damaged mufflers can restrict air
flow or cause excessive noise. Use air motors only with a filtered, lubricated and
regulated air supply. Dirty air, low-pressure air or over pressure air will cause malfunctions, including delayed starting.
AREA EQUIPMENT
Secure work. Whenever possible use clamps, vises, chains and straps to secure
pipe.
Make sure the tool is secured; it is safer to have both hands free to operate the tool.
TOOL USE
Use the right tool and tool bit for the job. Do not use a tool, which is incorrect for the
job you are doing.
Keep the tool bits fully engaged in the tool bit holders. Loose bits are a safety hazard.
4
92-0192 : Rev. 930618
Page 5
Model CBM-1 Counterboring Module
Disconnect power supply during setup and maintenance. Use all ‘Stop’ or Shut off’
features available when changing or adjusting tool bits, maintaining the tool, or when
the tool is not in use.
Remove adjusting keys and wrenches before applying power to the equipment.
Develop a habit of checking the tool before turning it on to make sure that all keys
and wrenches have been removed.
Do not force tools. Tools and tool bits function better and safer when used at the
feed and speed rate for which they were designed.
Do not reach into rotating equipment. Do not reach into the rotating head stock to
clear chips, to make adjustments, or to check surface finish. A machine designed to
cut steel will not stop for a hand or an arm.
Handle chips with care. Chips have very sharp edges and are hot. Do not try to pull
chips apart with are hands; they are very tough.
Avoid unintentional starts. Do not carry or handle tools with your hand on the operating switches or levers. Do not lay the tool down in a manner that will start the
drive. Do not allow the tool to flip around or move when adjusting or changing tool
bits.
Store idle tools properly. Disconnect tools from the power source and store in a safe
place. Remove tool bits for safe handling of the tool.
92-0192 : Rev. 930618
5
Page 6
TRI TOOL INC.
GENERAL DESCRIPTION
The CBM-1 C’bore Module is a mechanical accessory for the Tri Tool 601SBM,
602.5SBM and 602TSB Clamshells.
The C’bore Module provides the capability to counterbore pipe after an in-line spool,
valve or fitting has been removed.
The C’bore Module is mounted directly to the Tool Block.
No repositioning or modification of the Clamshell is necessary after in-line spool has
been removed.
The C’bore Module features a manual “easy grip” axial feed and infinitely adjustable
radial positioning.
The C’bore Module utilizes Form Tooling Bits which are available in various standard
configurations.
6
92-0192 : Rev. 930618
Page 7
Model CBM-1 Counterboring Module
SPECIFICATIONS
Counterboring Module
Weight: w/o Tool Block 2.0 lbs. (0.9 kg)
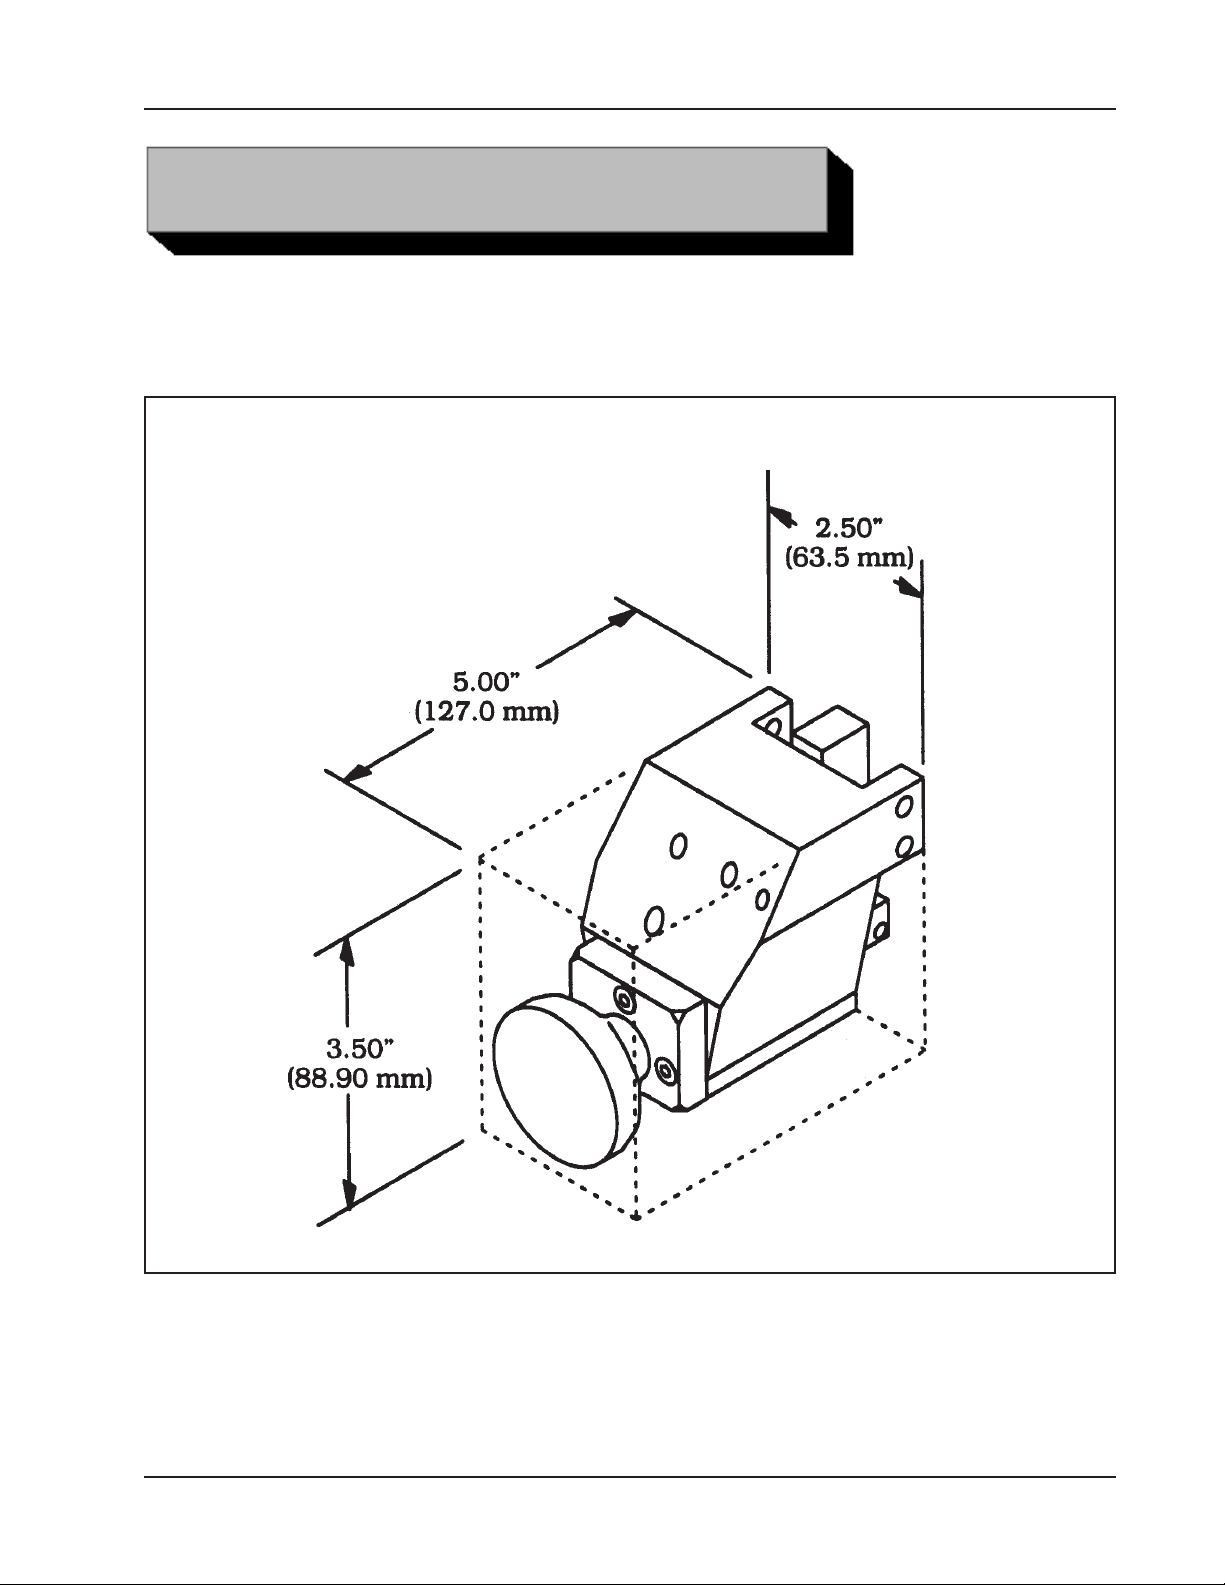
Envelope, Model CBM-1, Counterboring Module
Basic Pipe Sizes: 1” through 2 1/2” pipe all schedules and 3/4” pipe schedules 5S
through 40S with the appropriate Clamshell.
Counterbore Depth: Up to 1.13” (28.7 mm) plus lead out.
92-0192 : Rev. 930618
7
Page 8
TRI TOOL INC.
Clearances
Rotating Parts Diameter: Rotating diameter of clamshell.
Length: 6.60” (167.6 mm) from face of clamshell.
Axial Feed Length: 1.13” (28.7 mm)
Axial Feed Rate: .025” (.64 mm)/revolution
8
92-0192 : Rev. 930618
Page 9
Model CBM-1 Counterboring Module
MAINTENANCE
All components should be cleaned and coated with a light film of oil prior to storage.
Use a clean, non-detergent oil, preferable SAE 10 (90 SSU or lighter).
If the Counterboring Module is operated in such a way that the Module collects chips
or debris near the tool holder, the counterbore module should be cleaned after each
cutting operation.
Daily maintenance
Wipe the unit down and spray with rust preventative under severe humidity
conditions.
Visually inspect for loose screws, missing bolts, or damage due to impact.
Contact Tri Tool if major repair is required.
Tighten or replace screws or other parts as required.
Monthly Maintenance
Thoroughly clean and lubricate the Feed Screw and the Tool Bit Holder.
Feed the Tool Bit Holder out of the Tool Bracket.
With a clean, dry rag, thoroughly wipe down the Tool Bit Holder and the Feed
Screw.
Be sure that all old lubrication, chips, and dirt are completely removed.
Lubricate the Feed Screw and Tool Bit Holder with a light machine oil.
Reassemble the Tool Bit Holder into the Tool Bracket, being sure scribe line
on the Tool Bit Holder is facing the Cover Plate.
92-0192 : Rev. 930618
9
Page 10
TRI TOOL INC.
Read the operating instructions carefully before attempting to operate the CBM-1
C’bore Module.
Use eye protection at all times when operating the Counterbore Module.
Install the Clamshell on the pipe and remove the in-line spool, fitting etc. as
described in the appropriate Clamshell operating instructions.
Refer to the Operator’s Manual for operation of the 600 Series Clamshell, which is to
be used.
Slide the Mounting Adapter into the Tool Holder.
OPERATION
NOTE:
NOTE:
Tighten all Tool Holder Set Screws against the Mounting Adapter.
Mount the C’bore Module on the Mounting Adapter.
Secure the C’bore Module to the Tool Block.
Configure the C’bore Module.
Select the appropriate Tool Bit. Refer to the section on Tool Bits.
WARNING:
Install the Tool Bit in the Tool Bit Holder.
On Models 601SBM and 602.5SBM the Mounting Adapter is flush with the
back of the Tool Block.
On Model 602TSB the scribe line on the Mounting Adapter should be in-line
with the back of the Tool Block.
Use of dull or improperly designed Tool Bits or Tool Bits not manufactured by
Tri Tool Inc. may result in poor performance and may constitute abuse of this
machine and therefore voids the Tri Tool Inc. factory warranty.
10
Be sure the cutting edge lies along the radial centerline in the direction of rotation.
Adjust the counterbore diameter.
Radially adjust the C’bore Module using the Feed Sprocket.
92-0192 : Rev. 930618
Page 11
MACHINING SEQUENCE
Check to insure that the Tool Bits are clear of the pipe and that the Clamshell Feed
Pin is retracted.
Slowly rotate the clamshell to insure that the C’bore Tool Bit clears the pipe.
Increase the Clamshell RPM to cutting speed. Refer to section on Cutting Speeds.
To feed the Tool Bit in, hold the Feed Knob.
Model CBM-1 Counterboring Module
WARNING:
WARNING:
When the counterbore is finished, release the Feed Knob and allow the Clamshell to
rotate 2 or 3 times to release the chip.
Retract the Tool Bit.
Remove the C’bore Module from the Tool Block.
Remove the Clamshell from the pipe as described in the appropriate Clamshell
instruction manual.
Do not use a wrench or lever to obtain extra holding strength.
Do not force the feed, if the feed pressure builds up too high, release the
knob for 2 or 3 revolutions before continuing.
92-0192 : Rev. 930618
11
Page 12
TRI TOOL INC.
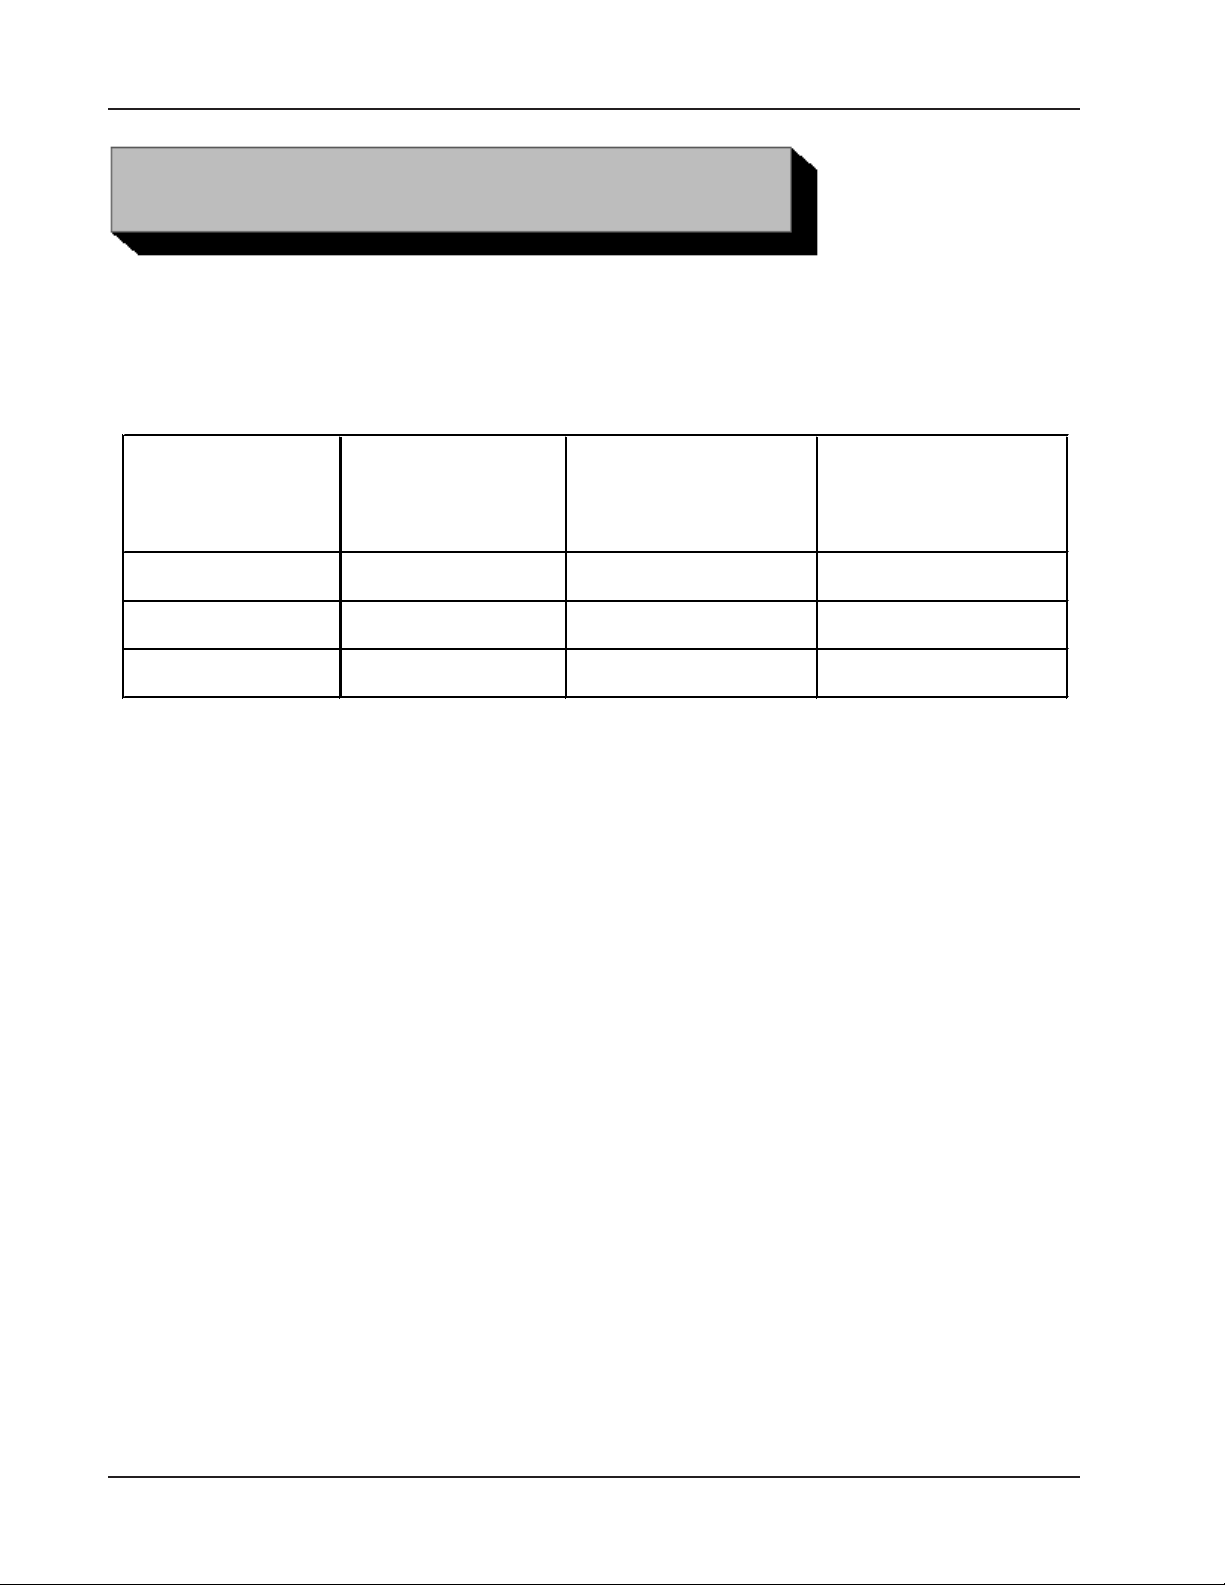
The chart shows RPM to obtain specified Tool bit surface cutting speed on the
surface of the pipe.
CUTTING SPEEDS
Cutting Speeds (Approx.)
RPM for
RPM for
RPM for
True
200 in/min.
250 in/min.
300 in/min.
Diameter
(508 cm/min.)
3" (76.2 mm) 21 27 32
2" (50.8 mm) 32 40 48
1" (25.4 mm) 64 80 95
Use 200 surface inches per minute (508 surface centimeters per minute)
For: Stainless steels in general when no coolant is allowed, all heavy-wall tube and
some of the chrome/molybdenum steels.
Use 250 surface inches per minute (635 surface centimeters per minute) for Mild
steels and some thin-wall stainless steels when coolants are permitted and applied.
Use 300 surface inches per minute (762 surface centimeters per minute) for
Aluminum and thin-wall mild steel and tube with coolants.
(635 cm/min.)
(762 cm/min.)
12
92-0192 : Rev. 930618
Page 13
Model CBM-1 Counterboring Module
TOOL BITS
Standard Tool Bits
Part
No. Description
99-2710 Tool Bit, C’bore
99-2715 Tool Bit, C’bore Extended, Double Cutting Edge
92-0192 : Rev. 930618
13
Page 14
TRI TOOL INC.
TROUBLE SHOOTING
Problem: The Tool Bit Chatters
The tool bit is loose or overextended.
The tool bit is damaged.
The tool holder is too loose in the slides.
The cutting speed is too fast.
The clamping pads are loose on the pipe or tube.
Cutting fluid is required.
The main bearing pre-load is loose.
Problem: There is excessive Tool Bit wear
The pipe or tube material is too hard or abrasive.
The cutting speed is too fast.
Cutting fluid is required.
A dull Tool Bit is causing surface hardening conditions (Stainless pipe or
tubing).
There is scale or other foreign matter on the pipe or tube, which is dulling the
tool bit at the start of the cut.
The tool bit is incorrect for the material being cut.
Problem: The surface finish is rough
The tool bit is dull, chipped, etc.
Metal build-up on the cutting edge of the tool bit is creating a false cutting
edge.
Cutting fluid is required.
Problem: The tool holder is not feeding
14
The feed pin is broken or out of position.
The feed sprocket shear pin is broken.
The feed screw is stripped.
The feed nut is stripped.
The slide rails are too tight.
92-0192 : Rev. 930618
Page 15
Model CBM-1 Counterboring Module
Problem: There is a loss of air power
The air supply pressure is too low.
The air filter is plugged.
The air line size is insufficient.
The air line is too long.
Problem: There is a loss of hydraulic power
The hydraulic supply pressure is too low.
The hydraulic filter is plugged.
The hydraulic line size is insufficient.
The hydraulic line is too long.
Problem: The tool bit will not reach the work
Incorrect tool blocks are installed for the size of the pipe or tube being
worked on.
Incorrect tool bit is installed.
Problem: The hydraulic motor will not start
The hydraulic power supply is shut off.
The hydraulic motor is damaged and will not run free.
92-0192 : Rev. 930618
15
Page 16
TRI TOOL INC.
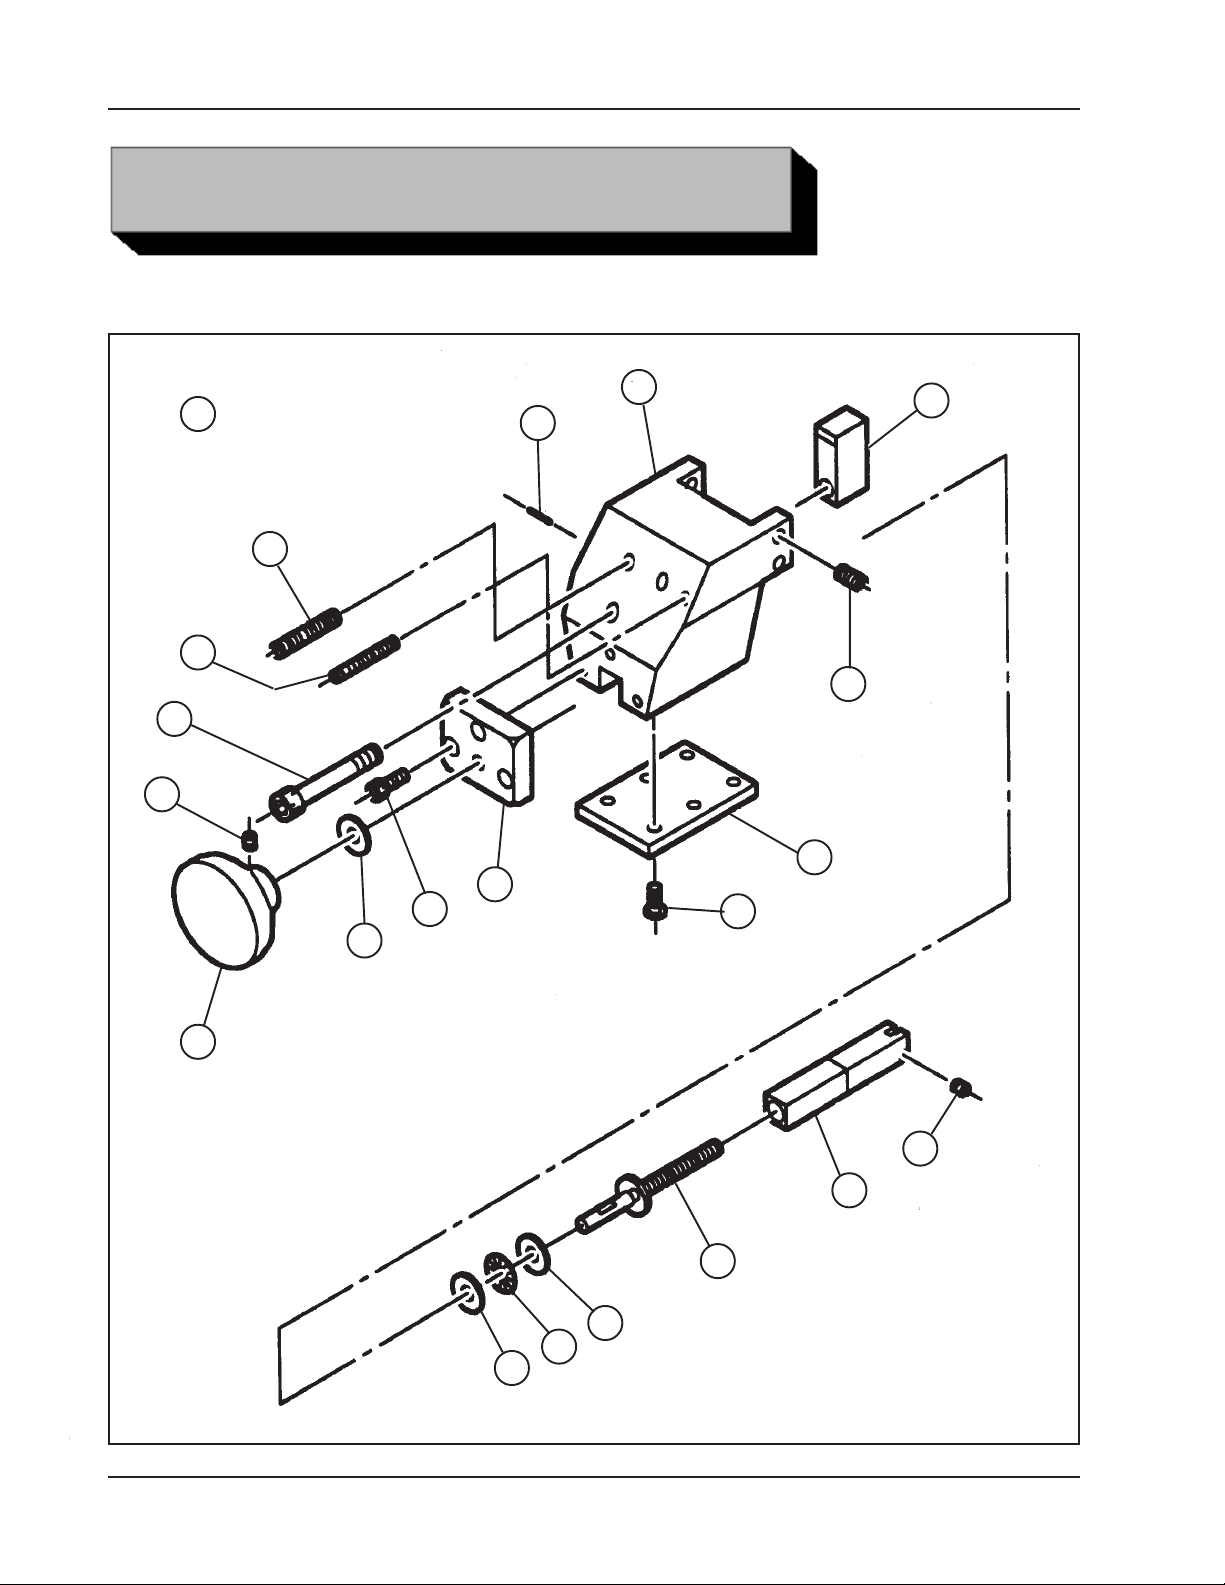
ILLUSTRATED PARTS BREAKDOWN
MODEL 600CBM-1, COUNTERBORING MODULE (P/N 82-0050)
11
19
Not Shown
1
14
12
8
7
16
6
13
3
2
9
4
16
18
10
20
15
17
5
17
92-0192 : Rev. 930618
Page 17
Model CBM-1 Counterboring Module
Parts List, Counterboring Module (P/N 82-0050)
Item Part
No. No. Description Qty
1. 08-0036 Tool Block Assy (601/602.5SBM) ref
08-0107 Tool Block Assy (602TSB) ref
2. 24-0705 Plate, Top 1
3. 24-0706 Plate, Cover 1
4. 27-0278 Adapter, Mounting ref
5. 29-0211 Bearing, Thrust 1
6. 32-0024 Pin Roll 1
7. 33-0028 Screw, Cap, 10-24 x 1/2 3
8. 33-0060 Screw, Cap, 5/16-18 x 2 1
9. 33-0280 Screw, Button, 10-24 x 5/8 6
10. 33-0487 Screw, Set, 10-24 x 3/16, Cup Pt 1
11. 33-0489 Screw, Set, 10-24 x 5/16, Cup Pt 1
12. 33-0497 Screw, Set, 10-24 x 1 1/4, Cup Pt 1
13. 33-0501 Screw, Set, 1/4-20 x 3/8, Cup Pt 4
14. 33-0510 Screw, Set, 1/4-20 x 1 3/4, Cup Pt 2
15. 33-1512 Screw, Feed, 1/4-40 1
16. 34-0218 Washer, Thrust 1
17. 34-0219 Washer, Thrust 2
18. 42-0100 Knob, Mod, Feed 1
19. 47-0420 Bracket, Tool 1
20. 49-0080 Holder Assy, Tool Bit 1
92-0192 : Rev. 930618
17
Page 18
TRI TOOL INC.
Parts List, C'bore Module Kit (P/N 05-0128)
Item Part
No. No. Description Qty
27-0278 Adapter, Mounting 1
82-0050 Module Assy, C’bore 1
99-2710 Tool Bit, C’bore 1
99-2715 Tool Bit, C’bore, Long 1
18
92-0192 : Rev. 930618
 Loading...