

Page 1
© 2014 TE Connectivity family of companies
All Rights Reserved
*Trademark
TE Connectivity, TE connectivity (logo), and TE (logo) are trademarks. Other logos, product, and/or company names may be trademarks of their respective owners.
TOOLING ASSISTANCE CENTER
1-800-722-1111
PRODUCT INFORMATION
1-800-522-6752
This controlled document is subject to change.
For latest revision and Regional Customer Service,
visit our website at www.te.com.
PROPER USE GUIDELINES
Cumulative Trauma Disorders can result from the prolonged use of manually powered hand tools. Hand tools are intended for occasional use and low
volume applications. A wide selection of powered application equipment for extended-use, production operations is available.
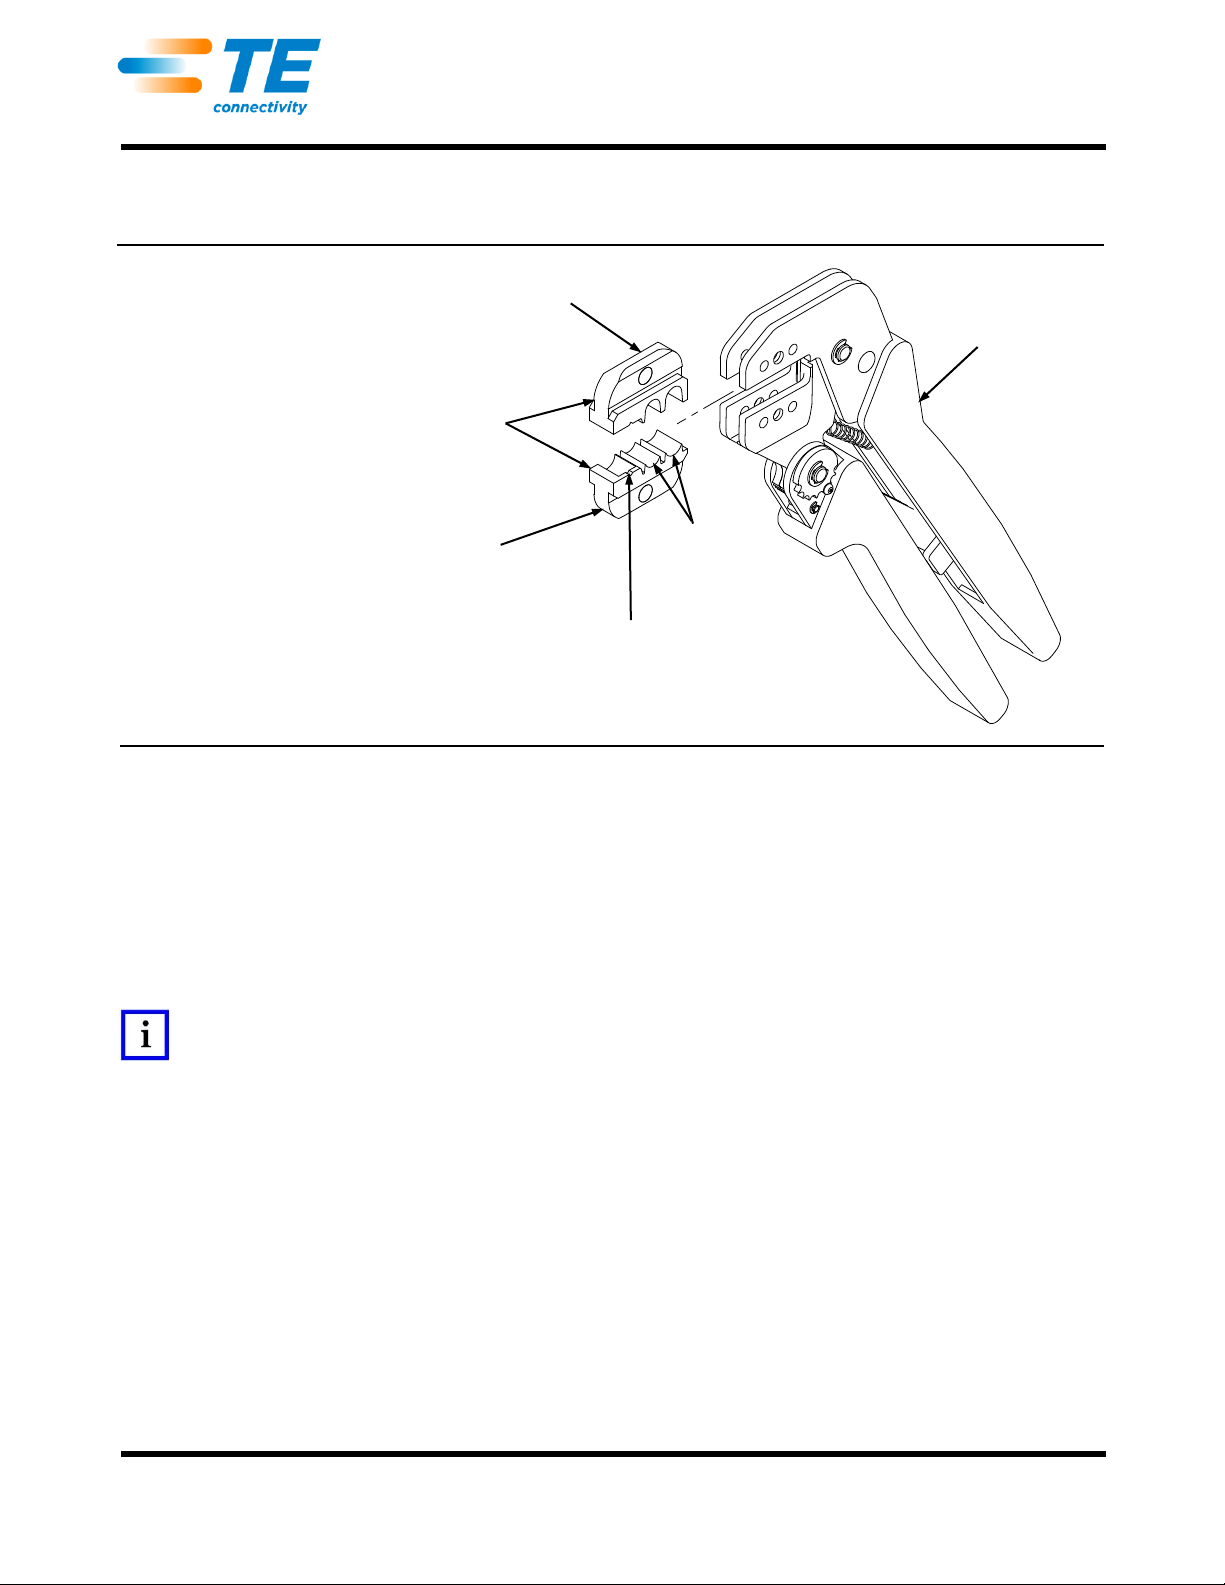
Crimping Die
Assembly 58536-1
The PRO-CRIMPER III Hand Tool is a “Commercial” grade tool and
is designed primarily for field installation, repair, maintenance work,
or prototyping in industrial, commercial, or institutional applications.
Product crimped with this tool will meet the crimp height requirement
for hand tools in the appropriate 114 application specification, but
may not comply with other feature parameters of the specification.
TE Connectivity offers a variety of tools to satisfy your performance
requirements. For additional information, contact the Technical
Assistance Center at 1-800-722-1111.
Indenter Die
Crimping Die
Assembly
58536-1
Anvil Die
Center Contact
Crimping Chamber
Ferrule
Crimping
Chambers
PRO-CRIMPER* III
Frame Assembly
354940-1 (Ref)
Instruction Sheet
408-4028
06 JUN 14 Rev B
Figure 1
1. INTRODUCTION
Crimping Die Assembly 58536-1 is designed to crimp 75-Ohm RF Series BNC Dual-Crimp Connectors when
used in PRO-CRIMPER III Frame Assembly 354940-1.
Catalog 82074 provides a guide for cable-to-connector selection. For connectors not referenced in the catalog,
contact TE Product Engineering for recommendations.
Reasons for reissue are provided in Section 8, REVISION SUMMARY.
NOTE
Dimensions in this instruction sheet are in millimeters [with inches in brackets]. Figures and illustrations are for reference only
and are not drawn to scale.
2. DESCRIPTION
The die assembly consists of an indenter die and an anvil die, which when closed form three crimping
chambers. The two larger crimping chambers crimp the ferrule of the connector onto the coaxial cable, and the
smaller crimping chamber crimps the center contact onto the center conductor of the coaxial cable. Each die is
held in the tool jaws by a single screw. See Figure 1.
3. DIE INSTALLATION (Figure 1)
1. Close the tool handles until the ratchet releases, then allow the tool handles to open fully.
2. Install anvil die in the movable jaw of the tool frame. Align the die with the retaining screw hole, then
secure die with the die-retaining screw. Do NOT fully tighten.
3. Install indenter die in the stationary jaw of the tool frame. Slowly close the tool handles, allowing the
dies to align themselves.
1 of 4
Page 2
408-4028
2 of 4
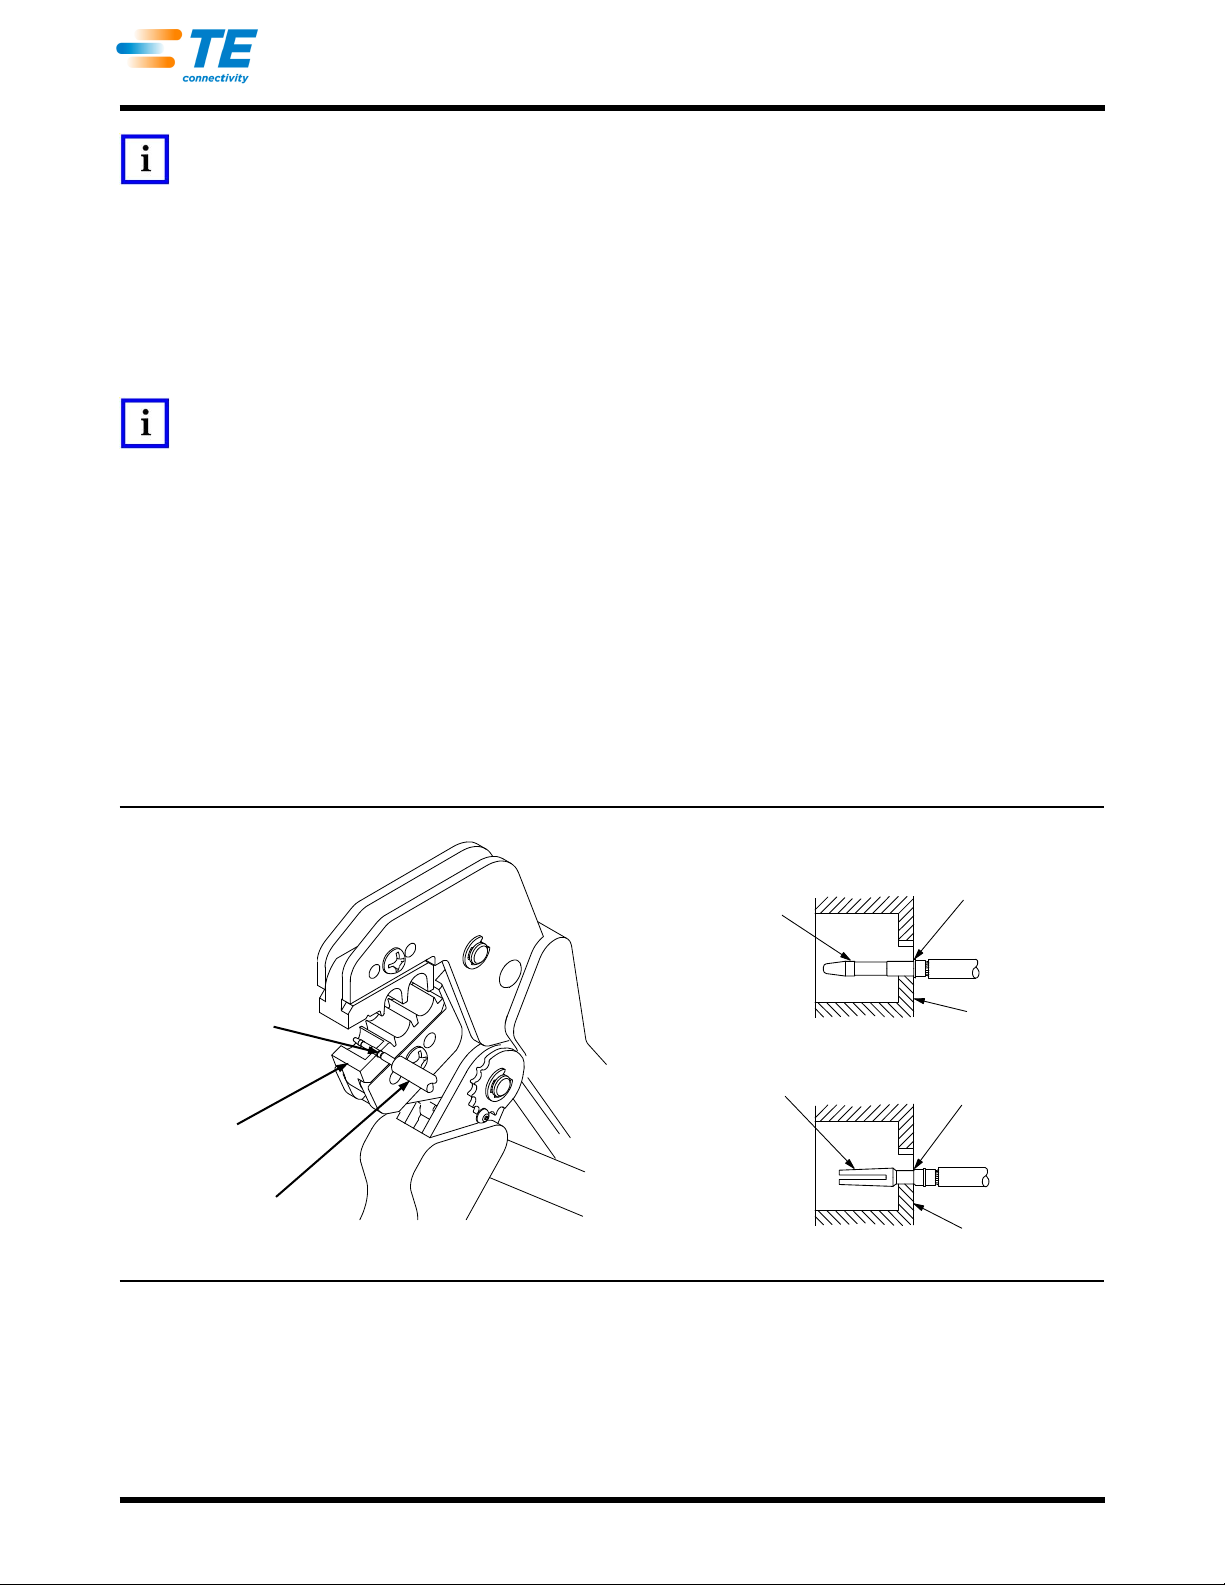
Crimping the
Center Contact
Flange on End of
Center Contact
Butts Against Die
Anvil Die
Stripped
Cable
Cross-Sectional View
Plug Contact
Jack Contact
Flange on
End of
Contact
Flange on
End of
Contact
Crimping Die
Crimping Die
NOTE
Once the anvil has entered the indenter, place a copper bus bar (1.5 ±0.05 [.062 ±.002] diameter) into the center contact
crimping chamber of the die assembly.
4. Close the tool handles completely.
5. Securely tighten both screws with the appropriate screwdriver.
4. CRIMPING PROCEDURE
Select the appropriate cable size and connector. The wire size and insulation diameter must be within the
specified range for the connector.
NOTE
This tool is provided with a crimp height adjustment feature. Initially, the crimp height should be verified. Refer to Section 5,
Crimp height Adjustment, to verify crimp height before using the tool.
For detailed information on cable strip lengths and proper assembly of the connector, refer to the instructions
packaged with the connector. Make sure that the connector's ferrule has been placed onto the cable, and that
the cable's braided shield is flared away from the cable. Then proceed as follows:
4.1. Crimping the Center Contact (Figure 2)
1. Close the tool handles until the dies are partially closed.
2. Assemble the center contact onto the cable center conductor and place the center contact in the
smallest crimping chamber of the anvil die. Make sure the flange on the end of the center contact
butts against the die.
3. Holding the cable in place, close the tool handles until the ratchet releases.
4. Allow the tool handles to open fully and remove the crimped center contact from the dies.
Figure 2
4.2. Crimping the Ferrule (Figure 3)
Rev B
1. Insert the crimped center contact into the connector body until the cable dielectric butts against the
dielectric inside the connector body or until the center contact is securely positioned within the
connector. Make sure that the braided shield is over the support sleeve of the connector body and that
no strands from the shield enter the connector body.
Page 3
408-4028
3 of 4
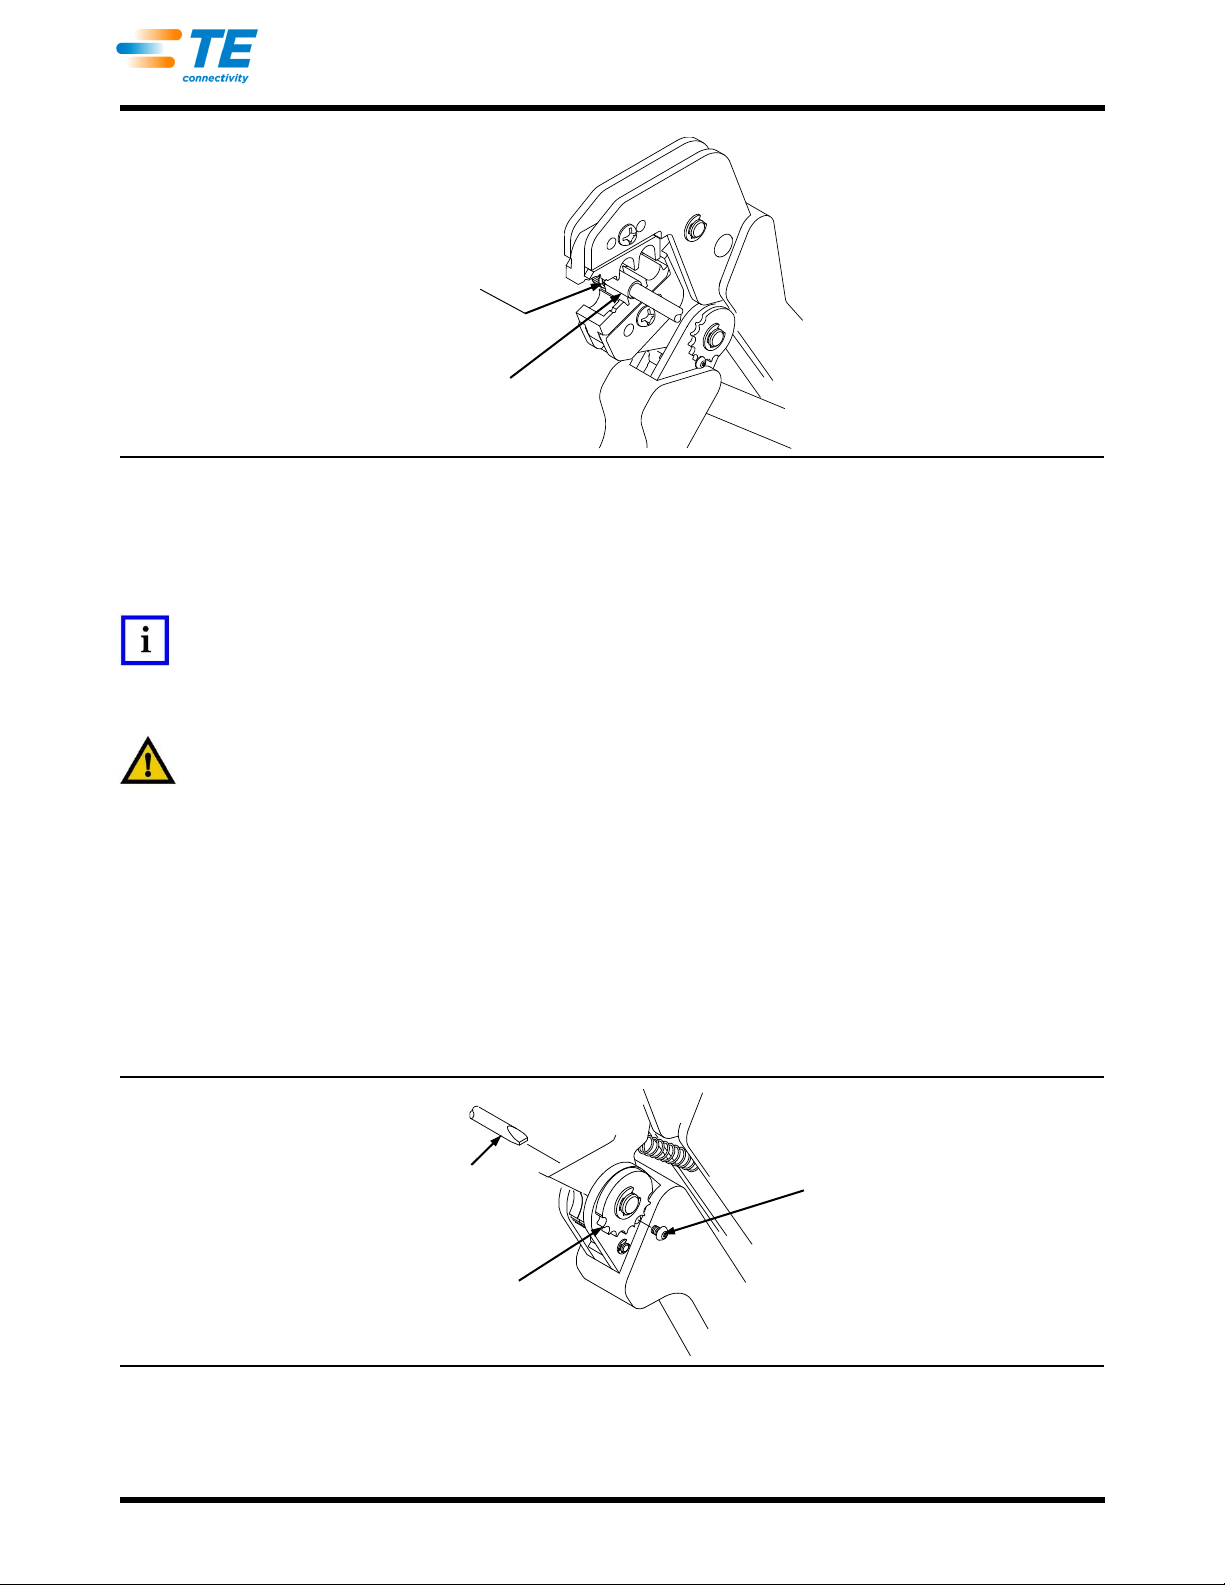
Crimping the
Ferrule
Shoulder on
Connector
Body Butts
Against Edge
of Die
Ferrule in
Crimping
Chamber on
Anvil Die
Screwdriver
Ratchet
Adjustment
Wheel
Lockscrew
(Typ)
Figure 3
2. Slide the ferrule up over the braided shield and onto the connector until the ferrule butts against the
shoulder on the connector body.
3. Place the ferrule in the appropriate crimping chamber of the anvil die so that the shoulder on the
connector body butts against the edge of the die.
NOTE
Refer to the instruction sheet packaged with the connector to determine the appropriate crimping chamber for the ferrule.
4. While holding the assembly together, begin to close the tool handles. Keep holding the assembly until
the dies have closed enough to clamp the assembly in place.
CAUTION
Make sure that both sides of the ferrule are started evenly into the crimping chamber. Do not attempt to crimp an improperly
positioned ferrule.
5. Carefully close the tool handles until the ratchet releases.
6. Allow the tool handles to open fully and remove the crimped connector from the dies.
5. CRIMP HEIGHT ADJUSTMENT (Figure 4)
The tool frame assembly ratchet mechanism features an adjustment wheel with numbered settings. If the crimp
height is not acceptable, adjust the ratchet as follows:
1. Remove the lockscrew from the ratchet adjustment wheel.
2. With a screwdriver, adjust the ratchet wheel from the opposite side of the tool.
Figure 4
3. Observe the ratchet adjustment wheel. If a tighter crimp is required, rotate the adjustment wheel
COUNTERCLOCKWISE to a higher- numbered setting. If a looser crimp is required, rotate the
adjustment wheel CLOCKWISE to a lower-numbered setting.
Rev B
Page 4
4 of 4
4. Replace the lockscrew.
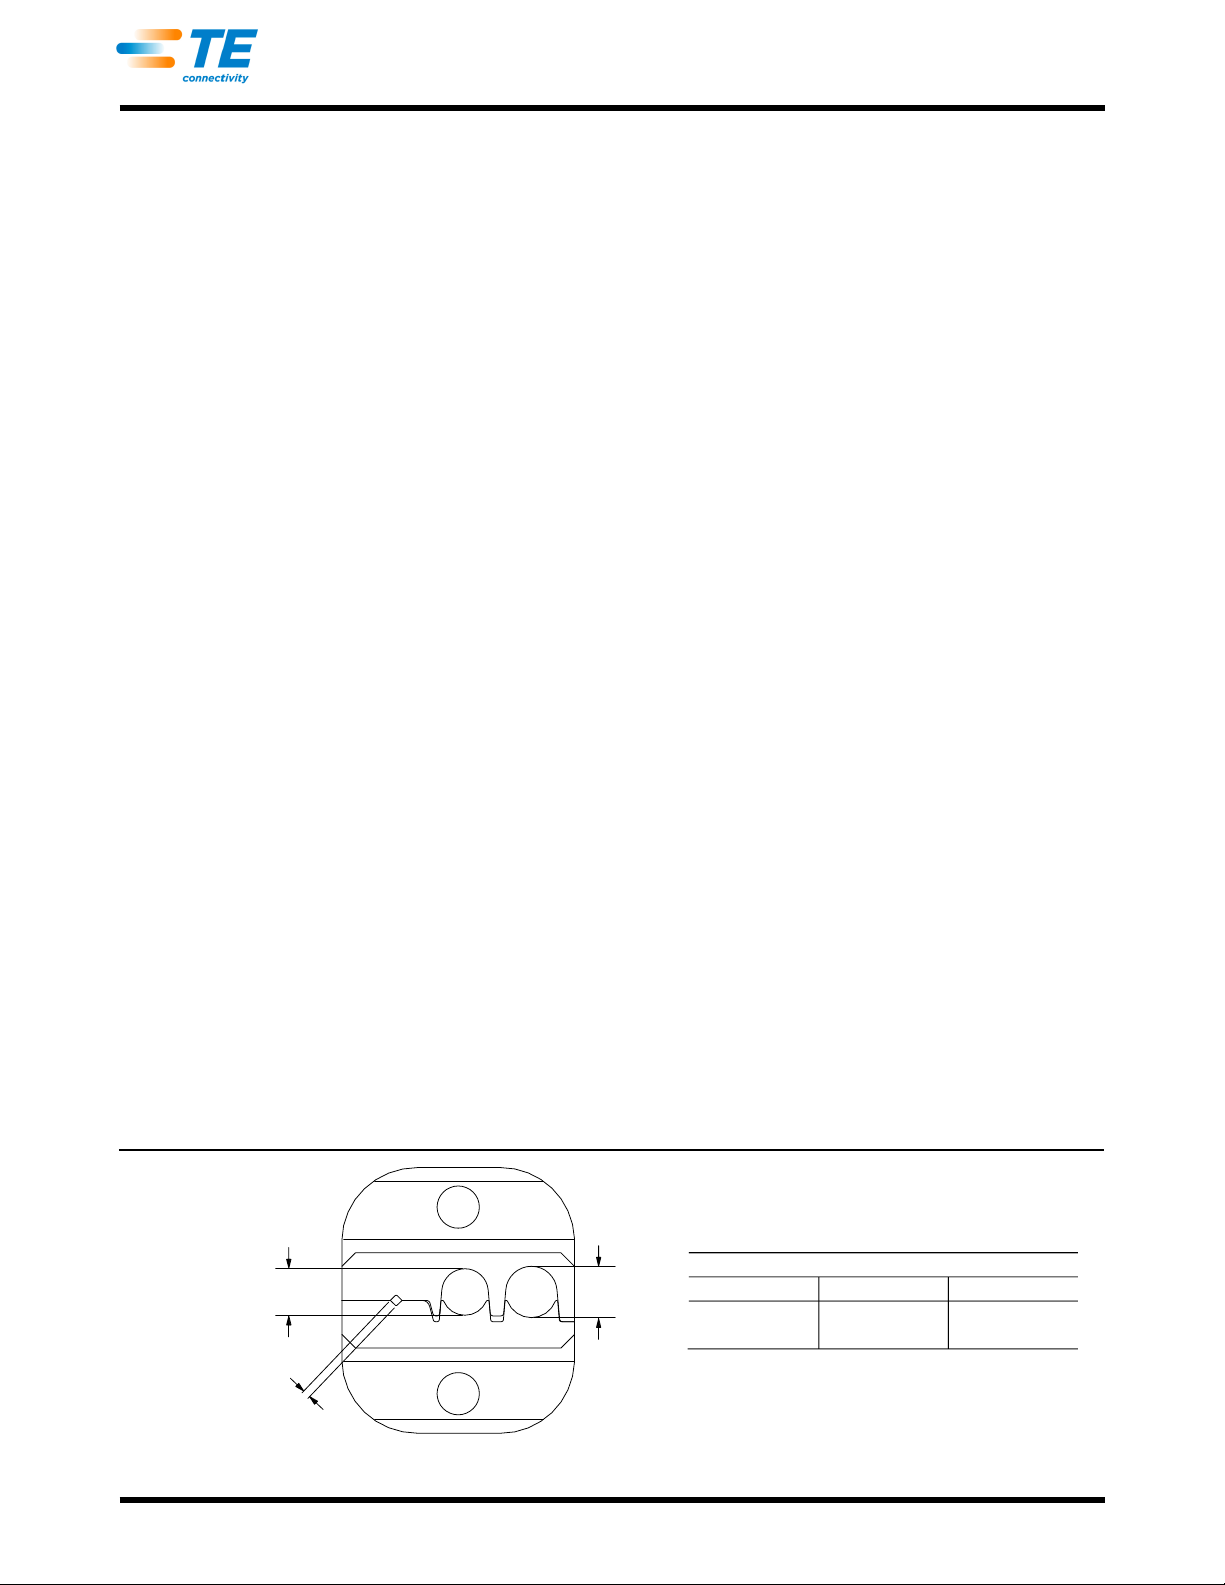
B (Ref)
DIE CLOSURE DIMENSIONS (mm [in.])
A B C
1.12 ±0.05
[.044 ±.002]
6.10 ±0.10
[.240 ±.004]
6.73 ±0.10
[.265 ±.004]
A (Ref)
C (Ref)
NOTE: Not to Scale
5. Make a sample crimp and measure the crimp height. If the crimp height is acceptable, secure the
lockscrew. If the dimension is unacceptable, remove lockscrew and continue to adjust the ratchet, and
again measure a sample crimp.
6. MAINTENANCE AND INSPECTION
6.1. Maintenance
1. Remove dust, moisture, and other contaminants with a clean, soft brush, or a clean, soft, lint-free
cloth. Do NOT use any objects that could damage the dies or tool.
2. Make sure that the proper die-retaining screws are properly secured.
3. When the dies are not in use, store them in a clean, dry area.
4. Store the tool with the tool handles closed to prevent objects from becoming lodged within the jaws.
6.2. Inspection
1. Remove all lubrication and accumulated film from the dies by immersing the dies in a suitable
commercial degreaser.
2. Make certain that all die-retaining screws and die components are properly secured.
3. Inspect the crimping surfaces for flattened, chipped, worn, or cracked areas. If damage is evident, the
dies must be replaced. Refer to Section 7, REPLACEMENT.
408-4028
6.3. Measuring Die Opening
The die assembly will perform correctly as long as: (1) the product specified is correct for the application, (2)
the specific die assembly is used, (3) the die assembly has been measured to ensure that the openings are
correct, and (4) the tool has been adjusted correctly. Figure 5 provides information on die opening sizes.
7. REPLACEMENT
Crimping Die Assembly 58536-1 is inspected before shipment. TE recommends that the dies be inspected
immediately upon arrival at your facility to ensure that the dies have not been damaged during shipment.
Order replacements through your local TE Representative, or call 1-800-526-5142, or send a facsimile of your
purchase order to 1-717-986-7605, or write to:
CUSTOMER SERVICE (038-035)
TYCO ELECTRONICS CORPORATION
PO BOX 3608
HARRISBURG PA 17105-3608
8. REVISION SUMMARY
Updated company logo
Rev B
Figure 5
Page 5
Mouser Electronics
Authorized Distributor
Click to View Pricing, Inventory, Delivery & Lifecycle Information:
TE Connectivity:
58536-1
 Loading...