

Page 1
MODEL TK-300U SERIES
TWO THREAD DOUBLE CHAINSTITCH HEAVY
DUTY MACHINE
INSTRUCTION MANUAL &
PARTS BOOK
TA KING INDUSTRIAL CO., LTD
Page 2
CONTENTS
INSTALLATION .............................................................................................................3
LUBRICATION.................................................................................................................4
OPERAOR INFORMATION .........................................................................................4-7
ADJUSTMENTS................................................................................................................7-14
INDEX
INSTALLATION .............................................................................................................3
LUBRICATION ...............................................................................................................4
ARM SHAFT ....................................................................................................................4
BED SHAFT .....................................................................................................................4
OTHER POINTS .............................................................................................................4
SPEED ...............................................................................................................................5
NEEDLES .........................................................................................................................5
SETTING ..........................................................................................................................5
THREADING ...................................................................................................................6
UPPER ..............................................................................................................................6
LOWER ............................................................................................................................6
PRESSER FOOT. PRESSURE .......................................................................................7
TENSION ..........................................................................................................................7
PRESSER BAR. HEIGHT ..............................................................................................8
STITCH LENGTH ..........................................................................................................8
FEED BAR. HEIGHT .....................................................................................................9
FEED DOG. CENTRALIZING ......................................................................................9
HEIGHT ...........................................................................................................................9
LENGTHWISE SETTING .............................................................................................9
SIDEWISE SETTING .....................................................................................................9
TIMING ..........................................................................................................................10
LOOP DEFLECTOR .....................................................................................................10
NEEDLE BAR. POSITION ..........................................................................................10
LOOPER. POSITIONING ............................................................................................11
LENGTHWISE SEETING ...........................................................................................11
SIDEWISE SETTING ...................................................................................................11
NEEDLE BAR. HEIGHT .............................................................................................11
TIMING ..........................................................................................................................12
NEEDLE GUARD .........................................................................................................12
SPREADER. POSITIONING.........................................................................................13
LENGTHWISE SETTING ...........................................................................................13
SIDEWISE AND HEIGHT SETTING .........................................................................13
T AKE-UP. ADJUSTMENT ...........................................................................................14
LOOPER THREAD .......................................................................................................14
NEEDLE THREAD .......................................................................................................14
RELEASER ....................................................................................................................14
1
Page 3
INTRUCTIONS FOR USING
ANTI-REVERSING MECHAINISM
ON MACHINES OF CLASSE 300U
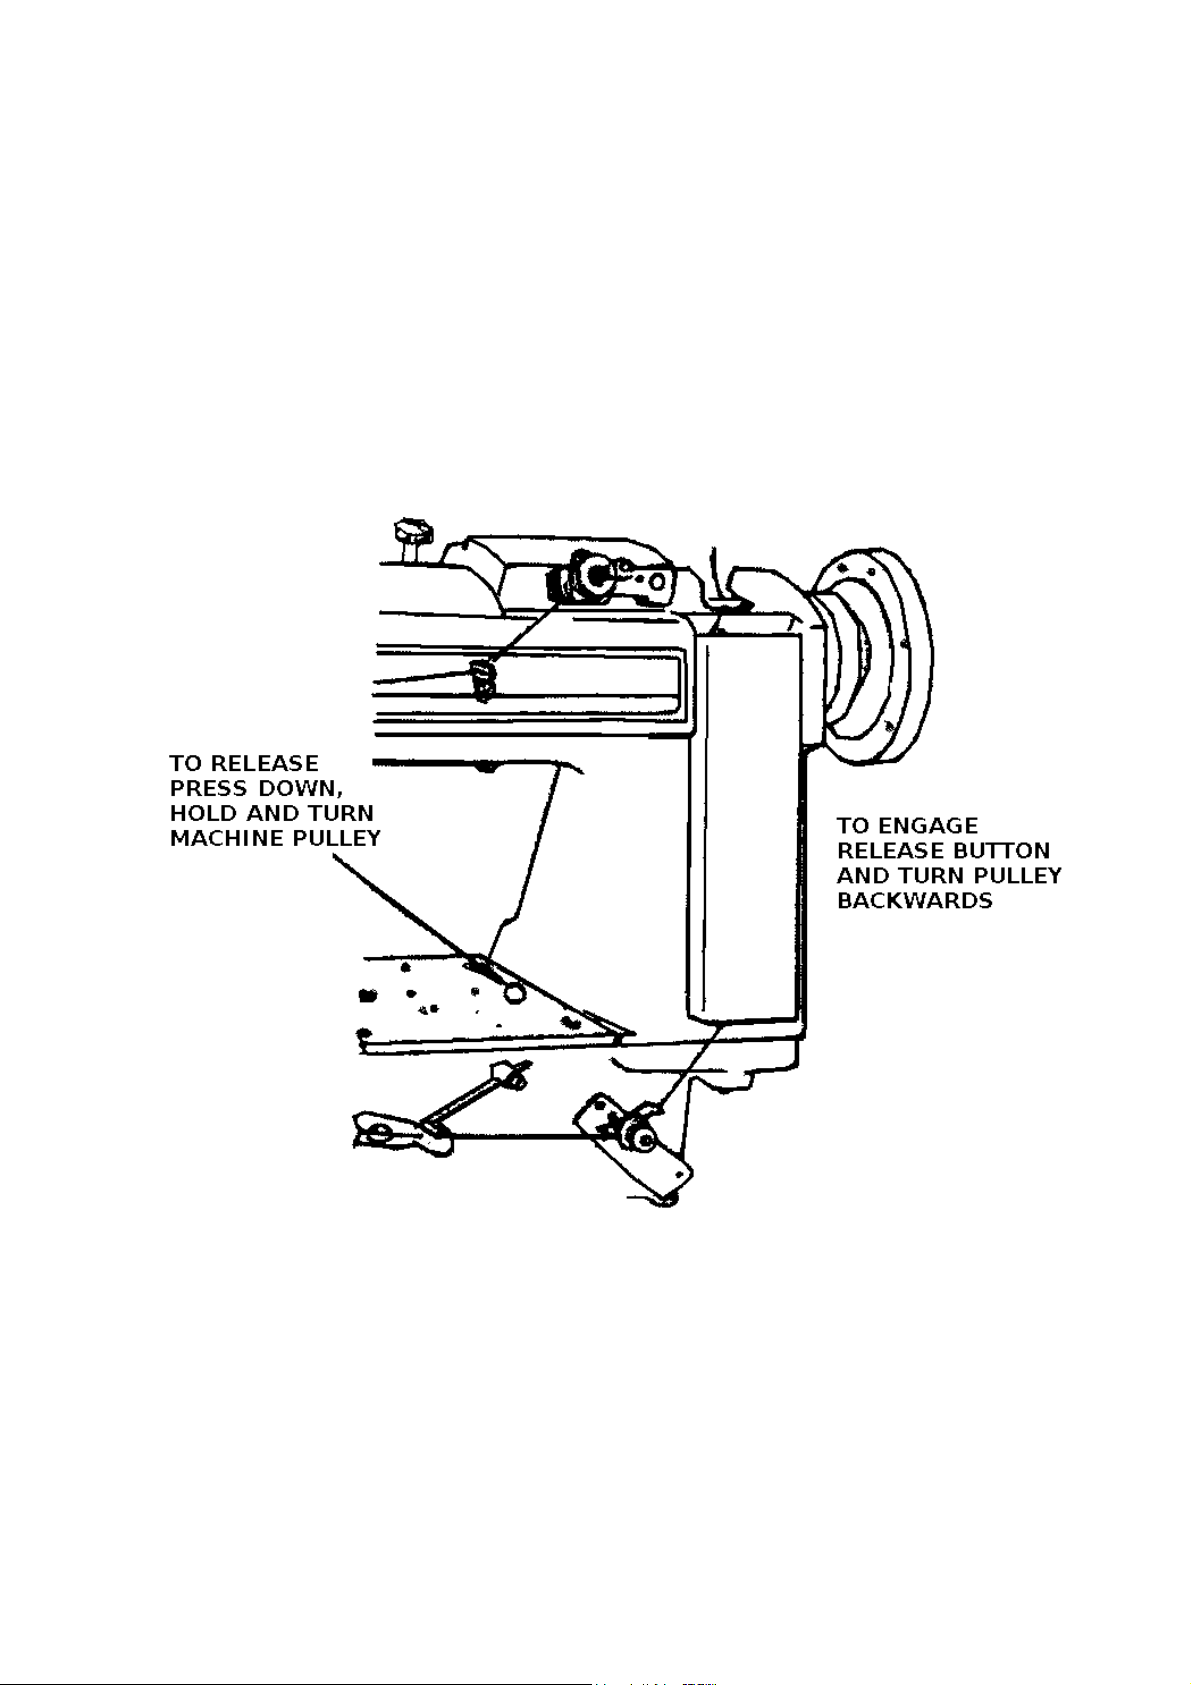
Machine 300U1C, are equipped with an ANTI-REVERSING device.
To release the device, depress button located on right side of bed plate, hold
down and turn machine pulley either forward or backward.
To engage the device, release button and turn machine pulley toward rear of
machine until device “snaps” into place.
EQUALIZING THE FEEDING MOVEMENT OF THE NEEDLE FEED AND DROP FEED ON
MACHINES OF CLASSE 300U
The needle feed and drop feed should not only be timed to move
simultaneously, but should also move the same distance during feeding. If the drop
feed moves a greater or less distance than the needle feed, depress the stitch length
button and turn the machine pulley, as required, to cause the drop feed movement to
equal the needle feed movement. The stitch length of both feeds can then be reset
simultaneously, as described on page 8.
2
Page 4
INSTALLATION
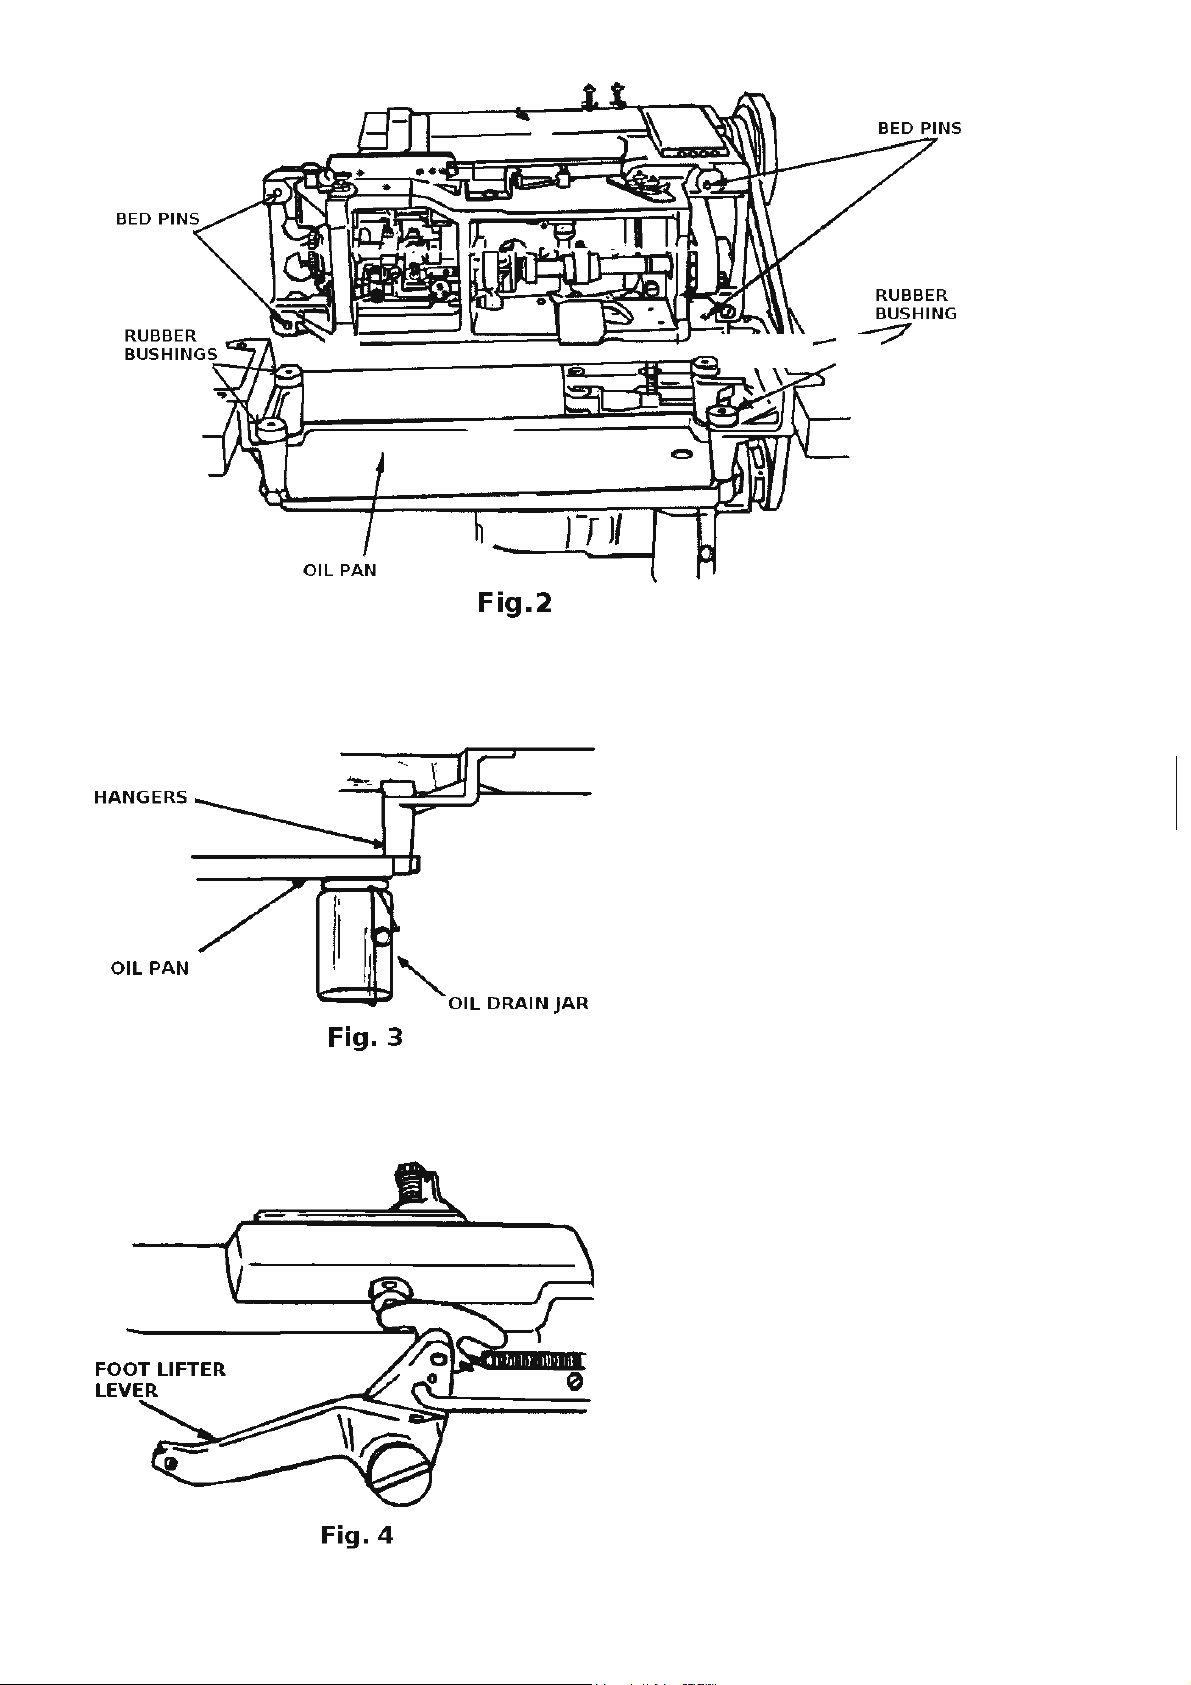
Assemble oil pan to hangers.
Insert assembled oil pan into
machine cut-out of table pacing four
rubber bushings in hanger holes as
shown in Fig. 2. Attach oil drain jar
to oil pan as shown in Fig. 3.
Place machine on oil pa
assembly with the four bed pins
passing through the four rubber
bushings shown in Fig. 2.
Connect foot lifter treadle to
foot lifter lever, Fig.4, at back of
machine by chain furnished for this
purpose.
3
Page 5
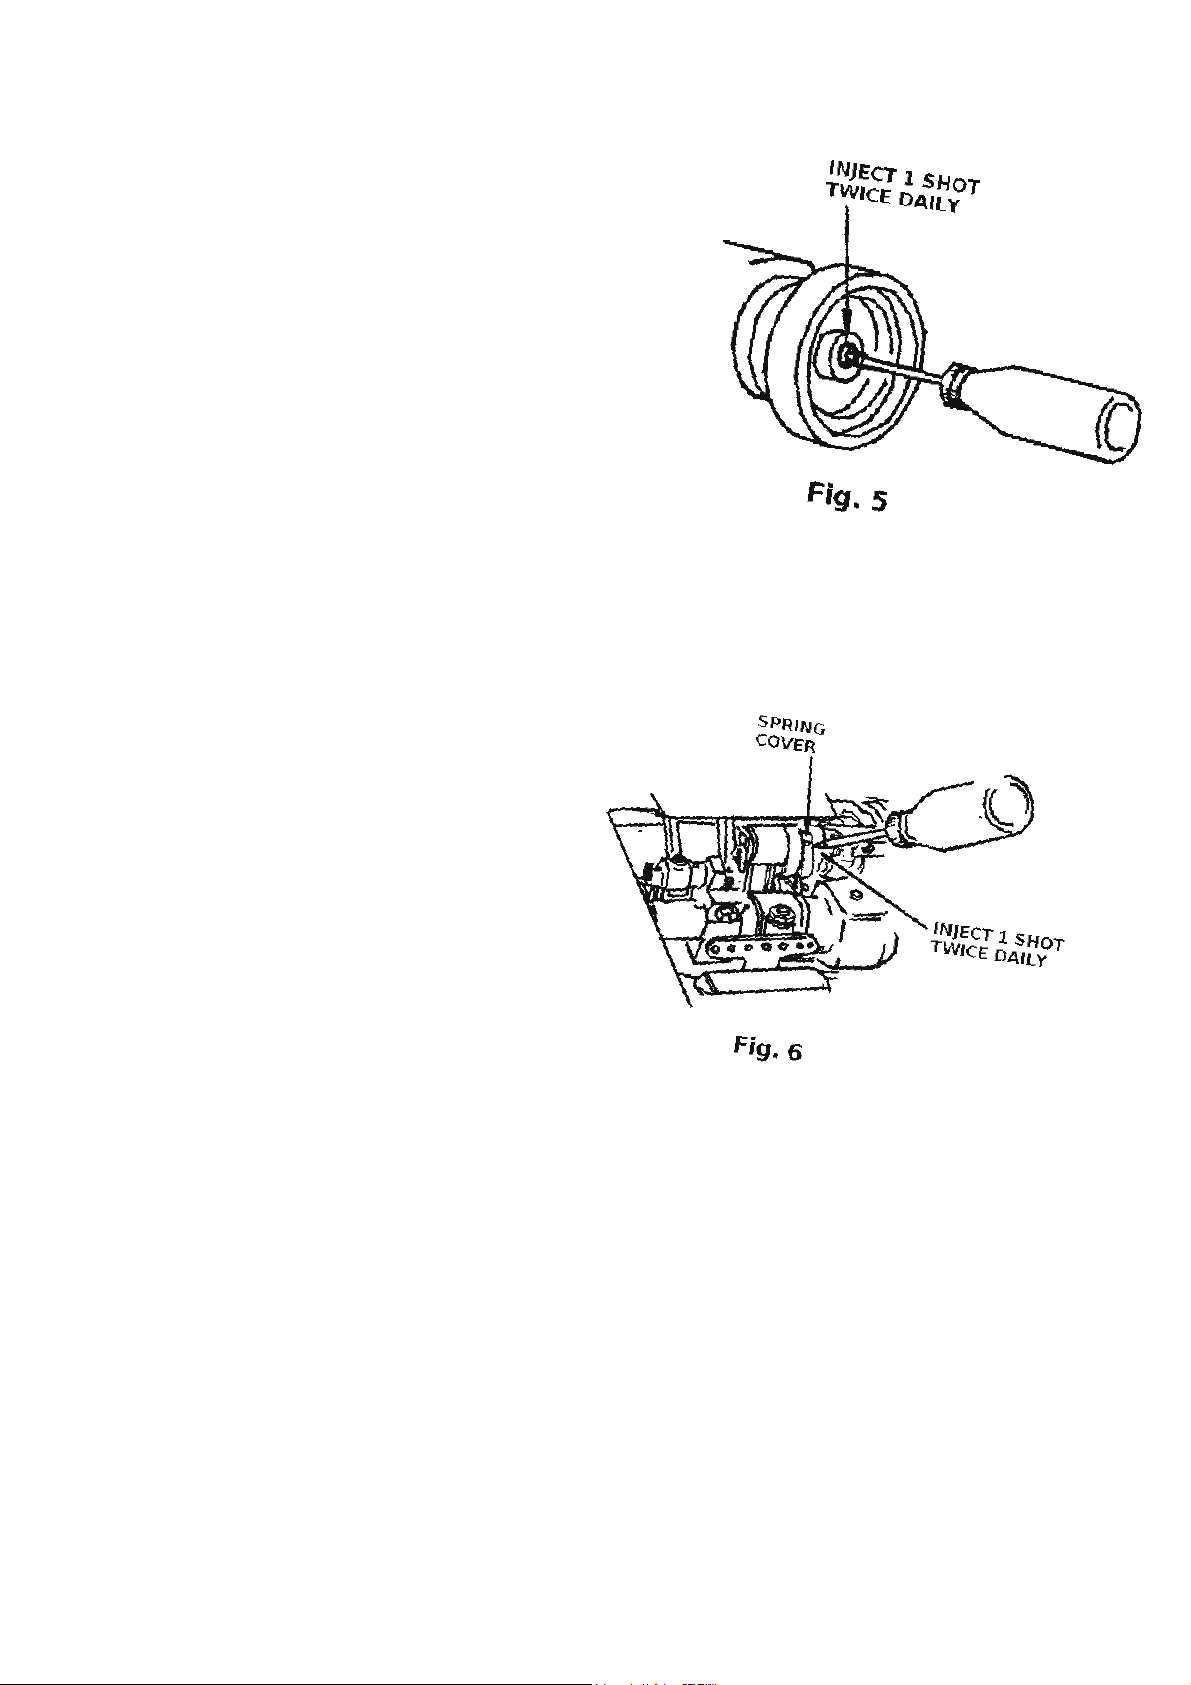
LUBRICATION
Machines of class 300U have a
semi-automatic lubricating system
comprising a hollow arm shaft and a
hollow bed shaft which act as oil
reservoirs. The oil is distributed to all of
the principal bearings by centrifugal force
through small jets in the shafts when the
machine is in operation. Provision is also
made of hand lubricating other movable
parts which are not lubricated from the
reservoirs.
Do not use additives in sewing
machine oil as they may cause a reduction
in the normal flow of oil that can result in
damage to the machine.
BEFORE STARTING machine, the
machine must be oiled as instructed.
Failure to do this will result in damage to
the machine.
Pressure Oil Can, furnished with the
machine, is to be used to oil all points
requiring lubrication.
TO OIL ARM SHAFT
To fill arm shaft reservoir, insert
spout of pressure oil can in hole, Fig.5,
and inject 1 shot of oil into shaft twice
daily.
TO OIL BED SHAFT
To fill bed shaft reservoir, push
spring cover, Fig. 6 , to the lef t, insert spout
of pressure oil can into hole and inject 1
shoe of oil into shaft twice daily. Close oil
hole spring cover.
NOTE: Bed shaft may also be oiled
from right hand end of machine.
OTHER OILING POINGS
Apply oil to all work plate and arm
oil holes, needle bar bearings and
connections, needle bar rock frame
bearings, looper rocker sleeve and
presser lifting mechanism.
CAUTION: For machines in
continuous use, all oiling points
must be oiled daily, Occasionally oil
tension release mechanism and looper
pull-out rack.
4
Page 6
For heavier weight material, needle
Catalog 4112 (62x59) may also be used. In
this cause, the needle bar must be adjust
as instructed on page 10.
The size of the needle to be used is
determined by the size of the thread which
must pass freely through the eye of the
needle.
Orders for needles should specify
quantity required, size number and catalog
number.
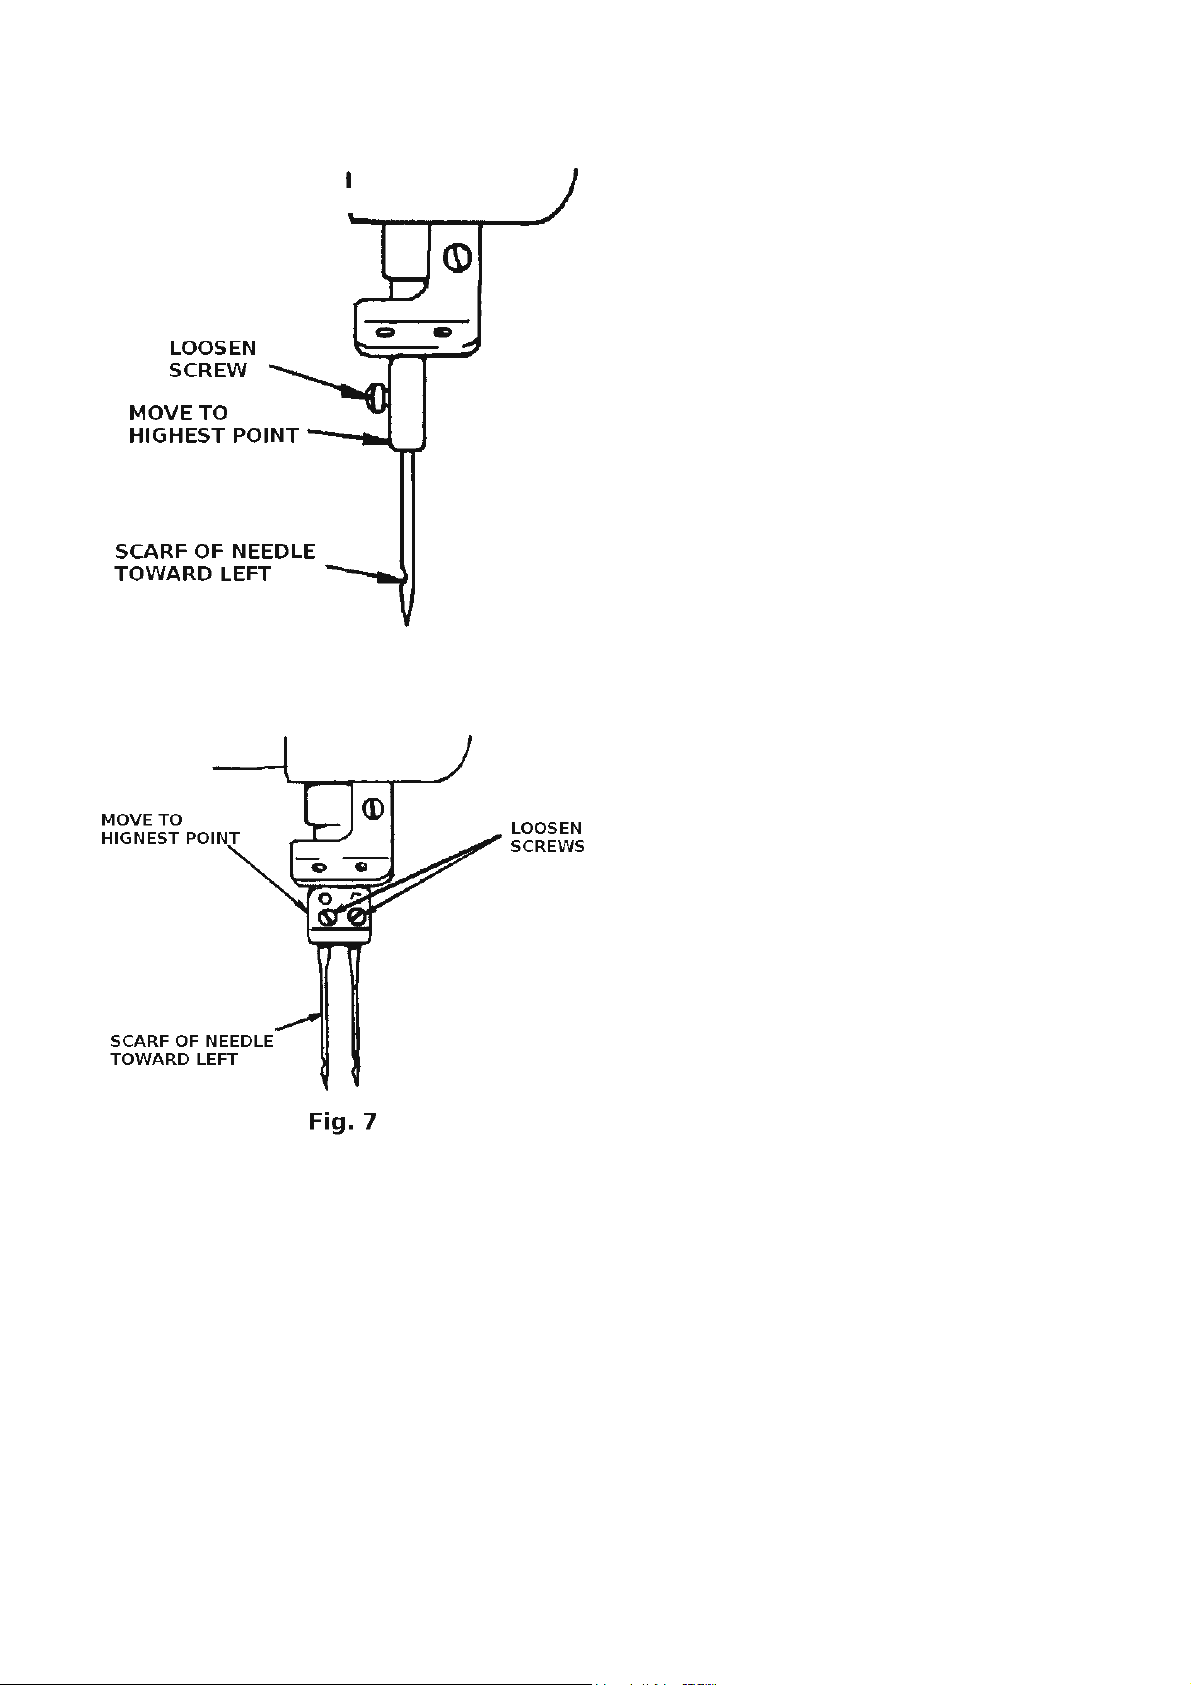
To Set The Needle
Turn machine pulley over toward the
operator until the needle bar is at its
highest point, as shown in Fig. 7.
Loosen needle set screw on single
needle machines or needle clamping
screws on multiple needle machines, as
shown in Fig. 7.
Insert needle into needle bar or
clamp as far as it will go making certain
that the scarf of each needle faces toward
the left, as shown in Fig. 7.
THREAD
Either left twist or right twist thread
may be used in the needles and loopers.
Rough or uneven thread, or thread
which passes through the needle eye with
difficulty will interfere with successful
operation of the machine.
5
Page 7
THREADING THE MACHINE
Upper Threading
Turn machine pulley over toward operator until needle bar is at its highest point.
Pass thread from unwinder through threading points indicated in Fig. 8. See
insert, Fig.8 for correct threading of needle.
Draw approximately two inches of thread through needle eye with which to start
sewing.
Single and multiple needle machines are all threaded as shown in Fig. 8. Make
certain that each thread passes through thread tension device.
Machines of Class 300U having Alternating Pressers are equipped with a thread
lubricator on front of the arm. The needle thread must pass though the lubricator.
Lower Threading
Open front table section, remove bed
slide and turn machine pulley over toward
operator until needle bar is at its highest
point.
Move loopers out of sewing position
by pulling looper throw-out gear locking
plunger rod and looper throw-out rack rod,
Fig. 8, out as far as possible. This will place
loopers in position for easier threading and
prevent accidental operation of machine
until loopers are returned to sewing
position.
Threading The Loopers
Pass thread form unwinder through
threading points as indicated. Draw
approximately two inches of thread
through looper eye with which to start
sewing.
6
Page 8
TENSION
Tension on thread should be light as
possible while still sufficient to set the
stitch correctly in material.
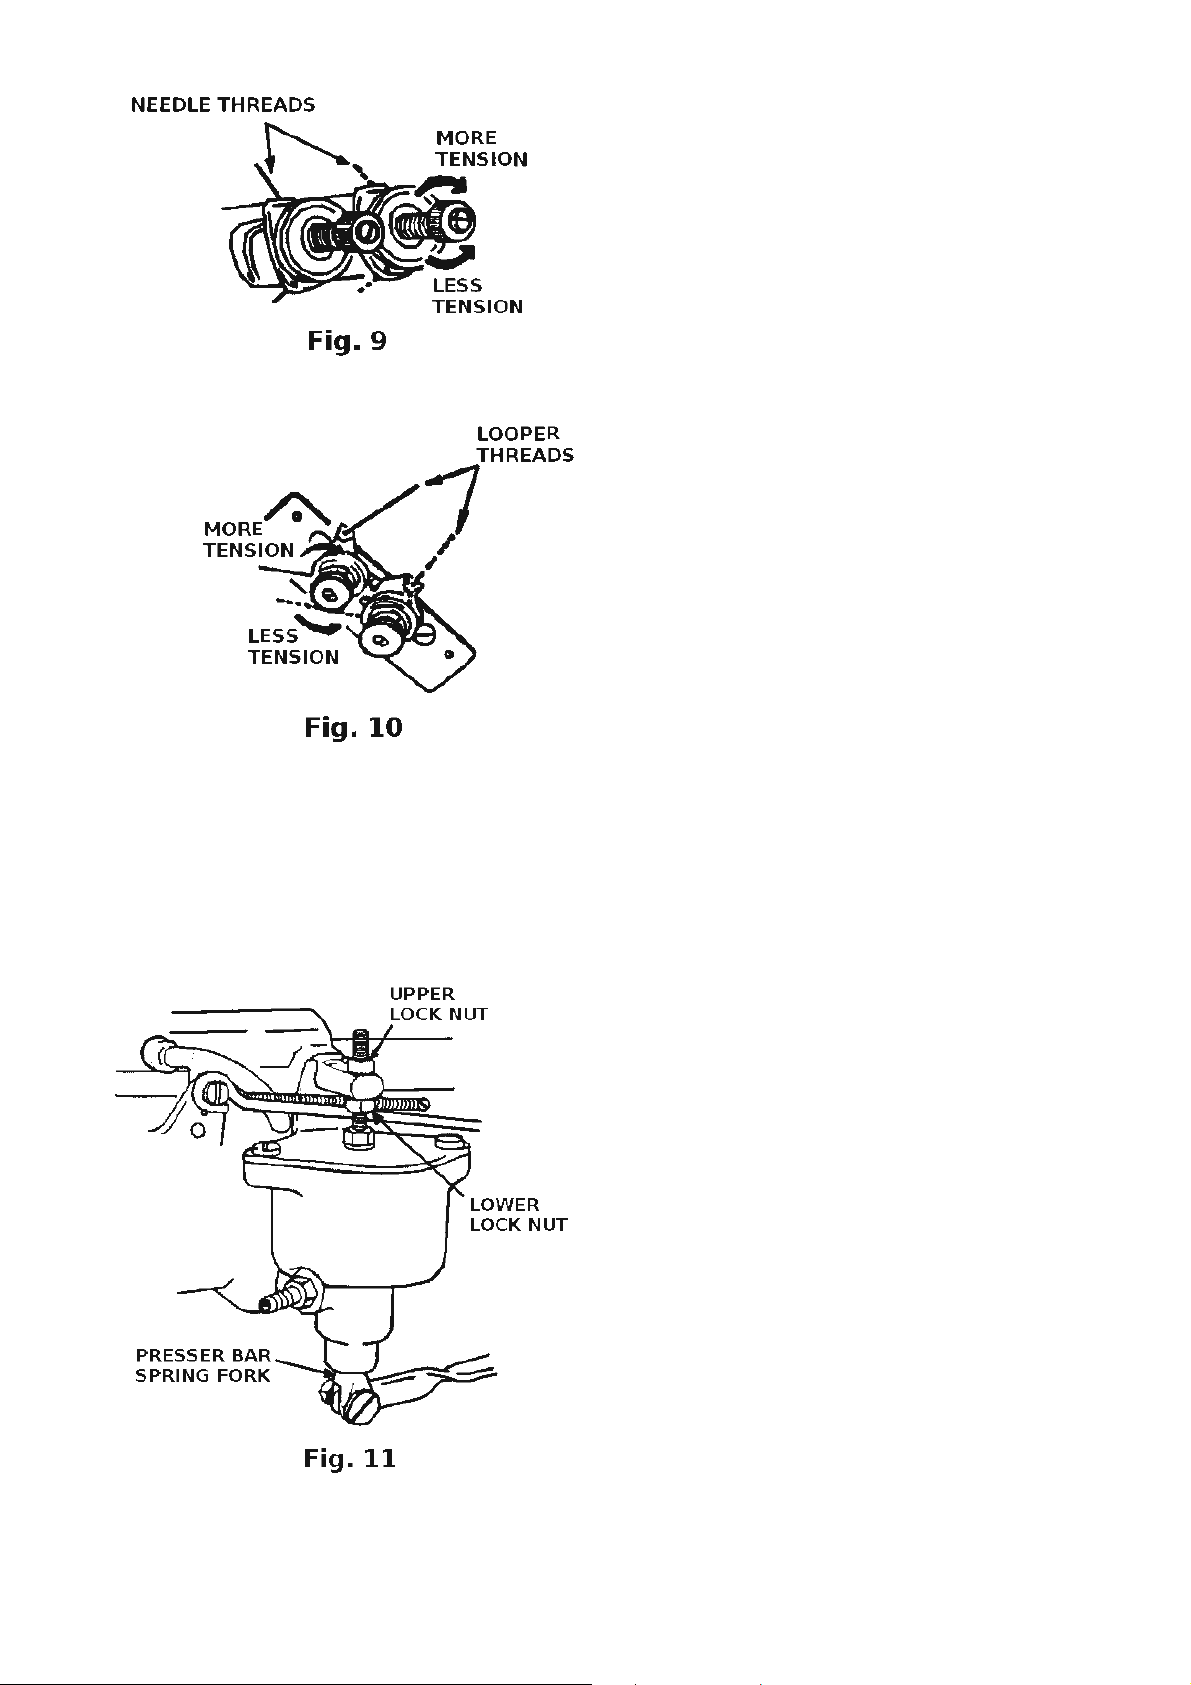
Needle Thread Tension
To regulate needle thread tension,
turn thumb screw, indicated in Fig. 9, as
may be required.
IMPORTANT: Regulate needle
thread tension only when presser foot is
down.
Looper Thread Tension
To regulate looper thread tension,
turn thumb screws, as indicated in Fig. 10,
as may be required.
Altemating Presser with
Penumatic Pressure Control:
Adjust height of Pressure Cylinder
with presser feet resting on throat plate.
There should be a clearance of 6.4mm
between the Presser Bar Spring Fork and
the bottom of the cylinder. To raise
cylinder, loosen lower lock nut and tighten
upper lock nut, see Fig. 11. To lower
cylinder , lossen upper lock nut and tighten
lower lock nut. When correct adjustment is
attained,k tighten both lock nuts.
Resulate air pressure. The correct air
pressure is set for average feeding when
the Presser bar spring For rises to
approximately 1.9mm from the bottom of
the cylinder.
7
Page 9
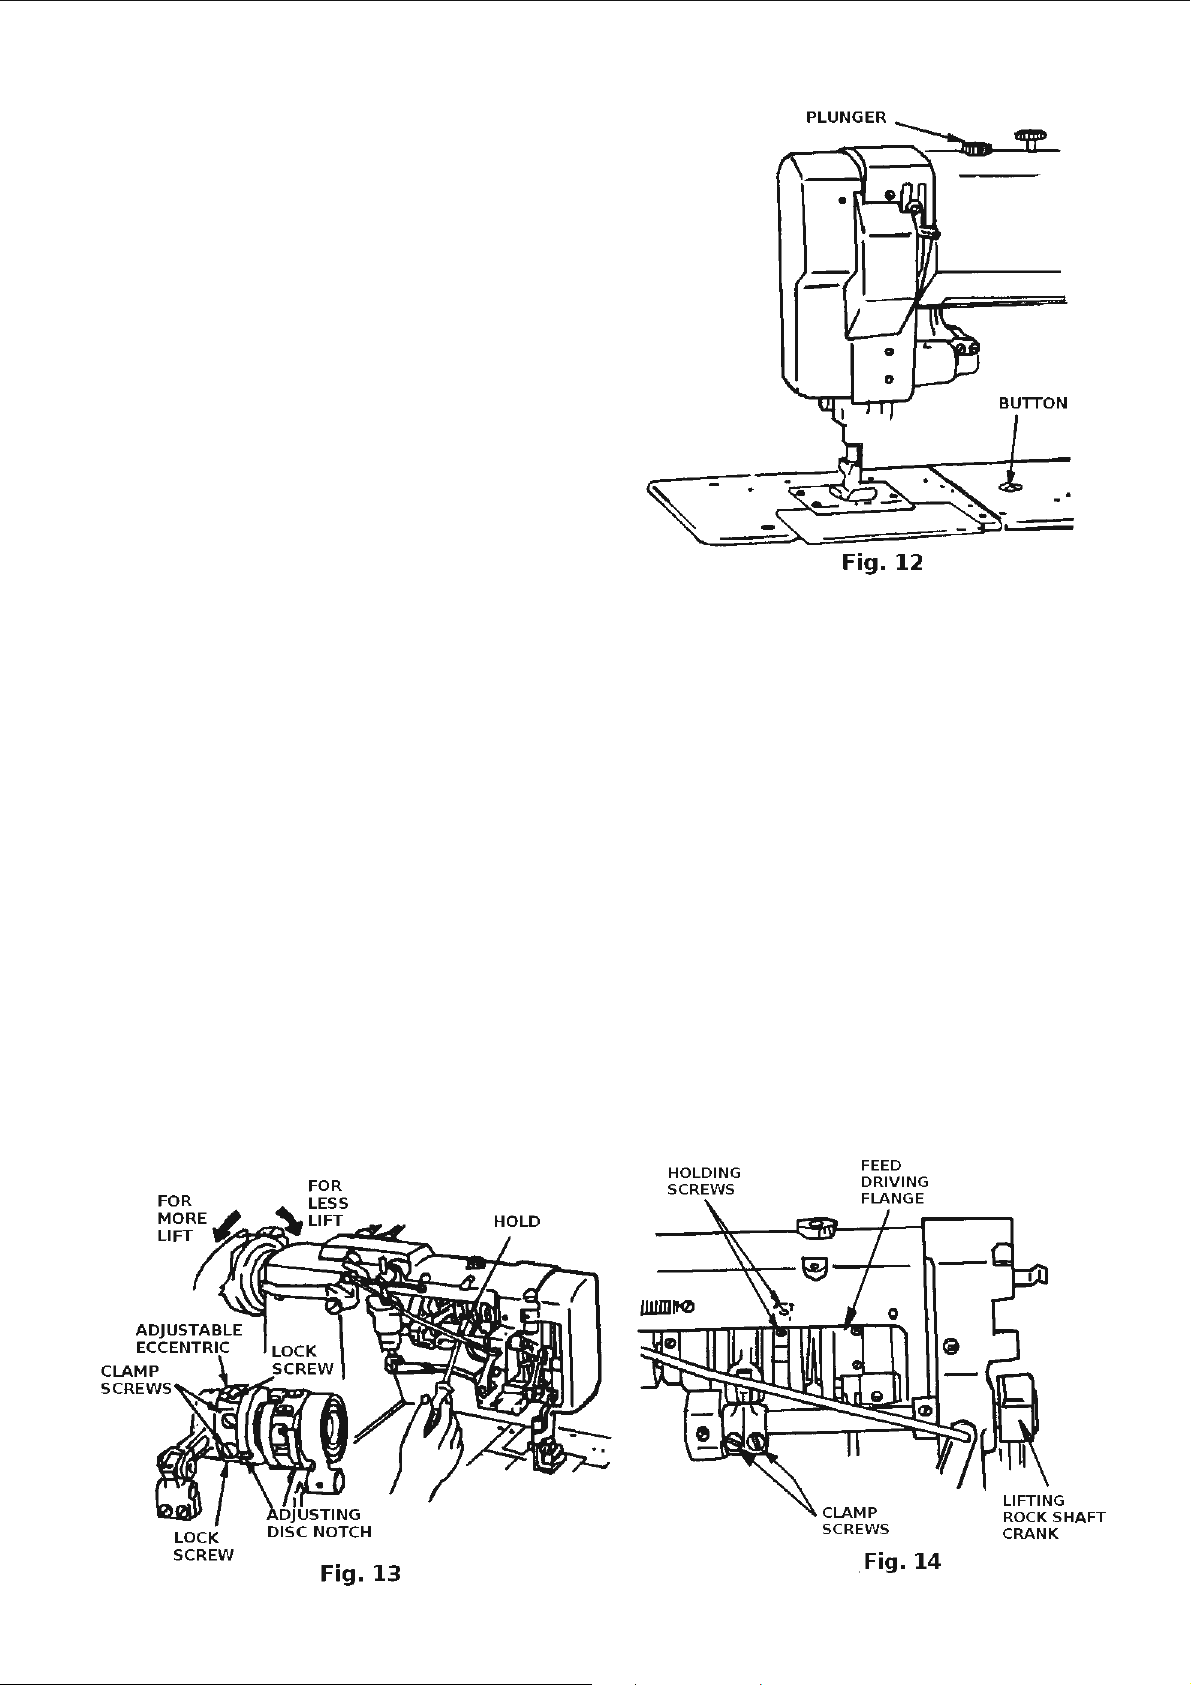
STITCH LENGTH
To adjust the stitch length, depress
plunger, Fig. 12, located on top of arm.
Continue to hold plunger down and turn
machine pulley toward operator until
plunger enters notch in arm shaft
eccentric. Then turn plunger to lock in
position. Depress button, Fig 12, located
on machine bed. Hold down, and turn
machine pulley toward operator to
increase length of stitch, or away from
operator to decrease length of stitch, letter
“A’ on machine pulley indicates the
longest stitch. When desired length,
indicated by letter, is opposite arrow on
front of machine, release button and turn
plunger to right or left until it springs
outward.
Machines with Alternating Pressers
The lift of the vibrating and lifting
pressers is controlled by an adjustable
eccentric. To adjust, remove arm cover at
rear of machine. Turn machine pulley over
toward operator until feeding presser is
down. Loosen the two lock screws, Fig. 13,
and the two clamp screws. Insert screw
driver into notch of adjusting disc, and
turn machine pulley as indicated in Fig. 13.
Then tighten the two clamp screws and
the two lock screws.
When it is desirable to have either
one of the pressers lift higher than the
other, turn machine pulley over toward
operator until the lifting presser is at its
highest position. Loosen the two clamp
screws, Fig.14, and turn lifting rock shaft
crank up or down until desired lift of each
presser is attained. Then tighten the two
clamp screws
CAUTION: Limit lift of
pressers to minimum required for the
work, as this permits higher speeds.
The vibrating presser should be
timed so that under normal sewing
conditions, the presser foot will seat
on the material at approximately the
same time the needle enters material.
This timing can be advanced or
retarded slightly depending on the
type of operation being performed,
such as sewing over seams. T o adjust,
loosen two holding screws, Fig. 14,
not more than one half turn. Then turn
the adjustable eccentric, Fig. 13, until
the vibrating presser seats at the
correct time. Securely tighten the two
holding screws after adjustment is
made.
8
Page 10
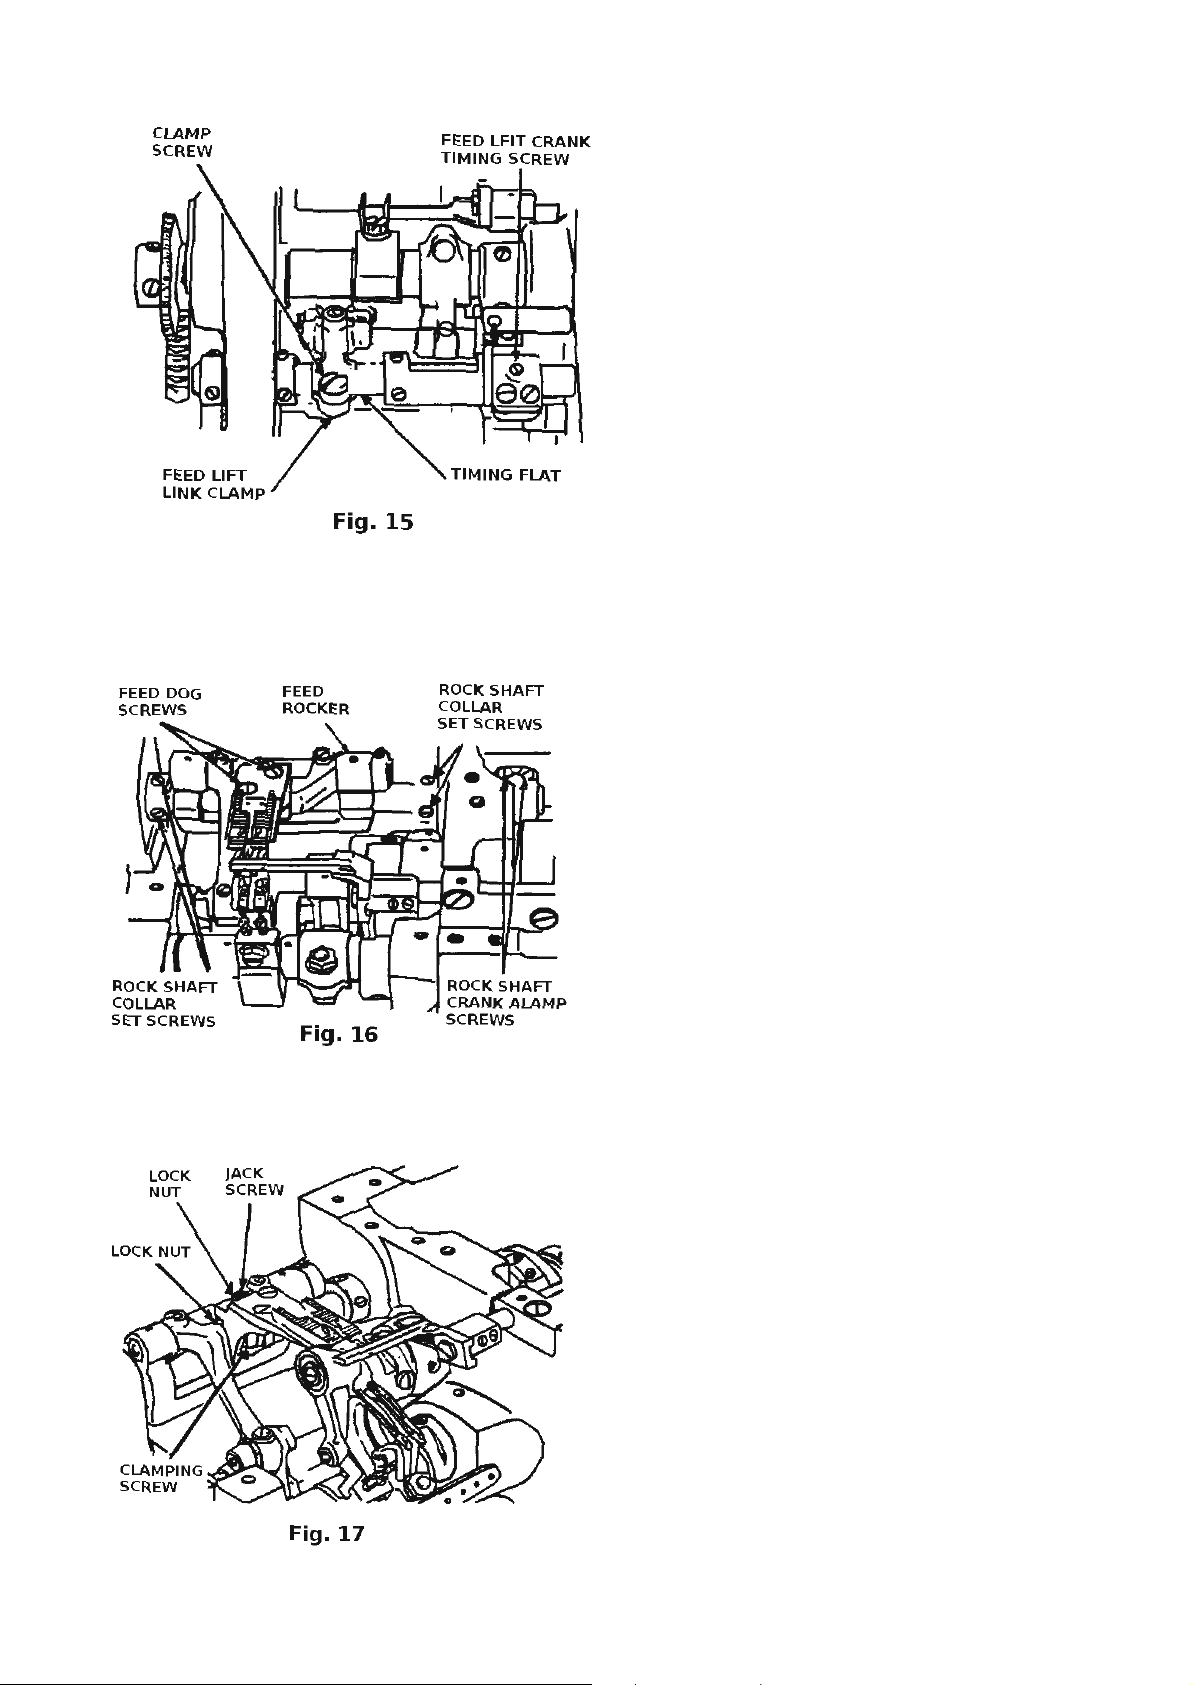
TO SET FEED BAR AT CORRECT HEIGHT
When the feed bar is set at the
correct height, the feed lift link clamp will
be aligned with the rock shaft timing flat.
To adjust, make certain that the feed lifting
crank timing screw, Fig.15, engages shaft
spot correctly. Loosen clamp screw and
move the feed lift clamp link to correct
position. The tighten clamp screw.
CENTRALIZING FEED DOG
Sidewise Setting
Needle should enter needle hole of
feed dog with the same clearance between
the needle and left or right side of hole. To
adjust, loosen feed dog screws, Fig. 16.
Move feed dog until correct clearance is
attained. Hold in position, and tighten feed
dog screws.
Additional adjustment, if necessary,
may be attained by loosening the four rock
shaft collar set screws, the two rock shaft
crank clamp screws. Fig. 16, and feed
lifting clamp screw, Fig. 15. Move
complete assembly to required position
and tighten screws.
Lengthwise Setting
The feed dog should clear the ends
of the feed slots in the throat plate equally
at both ends of feed travel. To adjust, set
feed for desired stitch length. Loosen the
two rock shaft crank clamp screws, Fig. 16.
Move feed rocker forward or backward
until correct positioning is attained. Then
tighten the two clamp screws.
SETTING FEED DOG AT CORRECT
HEIGHT
When the feed dog height is set
correctly, approximately the full depth of
the teeth will show above the throat plate.
To adjust, loosen lock nuts, Fig.17, and
slightly loosen feed dog clamping screw.
To raise feed dog turn jack screw
clockwise; to lower turn jack screw
counter-clockwise and tap feed dog down.
When correct setting is attained, tighten
the clamping screws and lock nuts.
9
Page 11
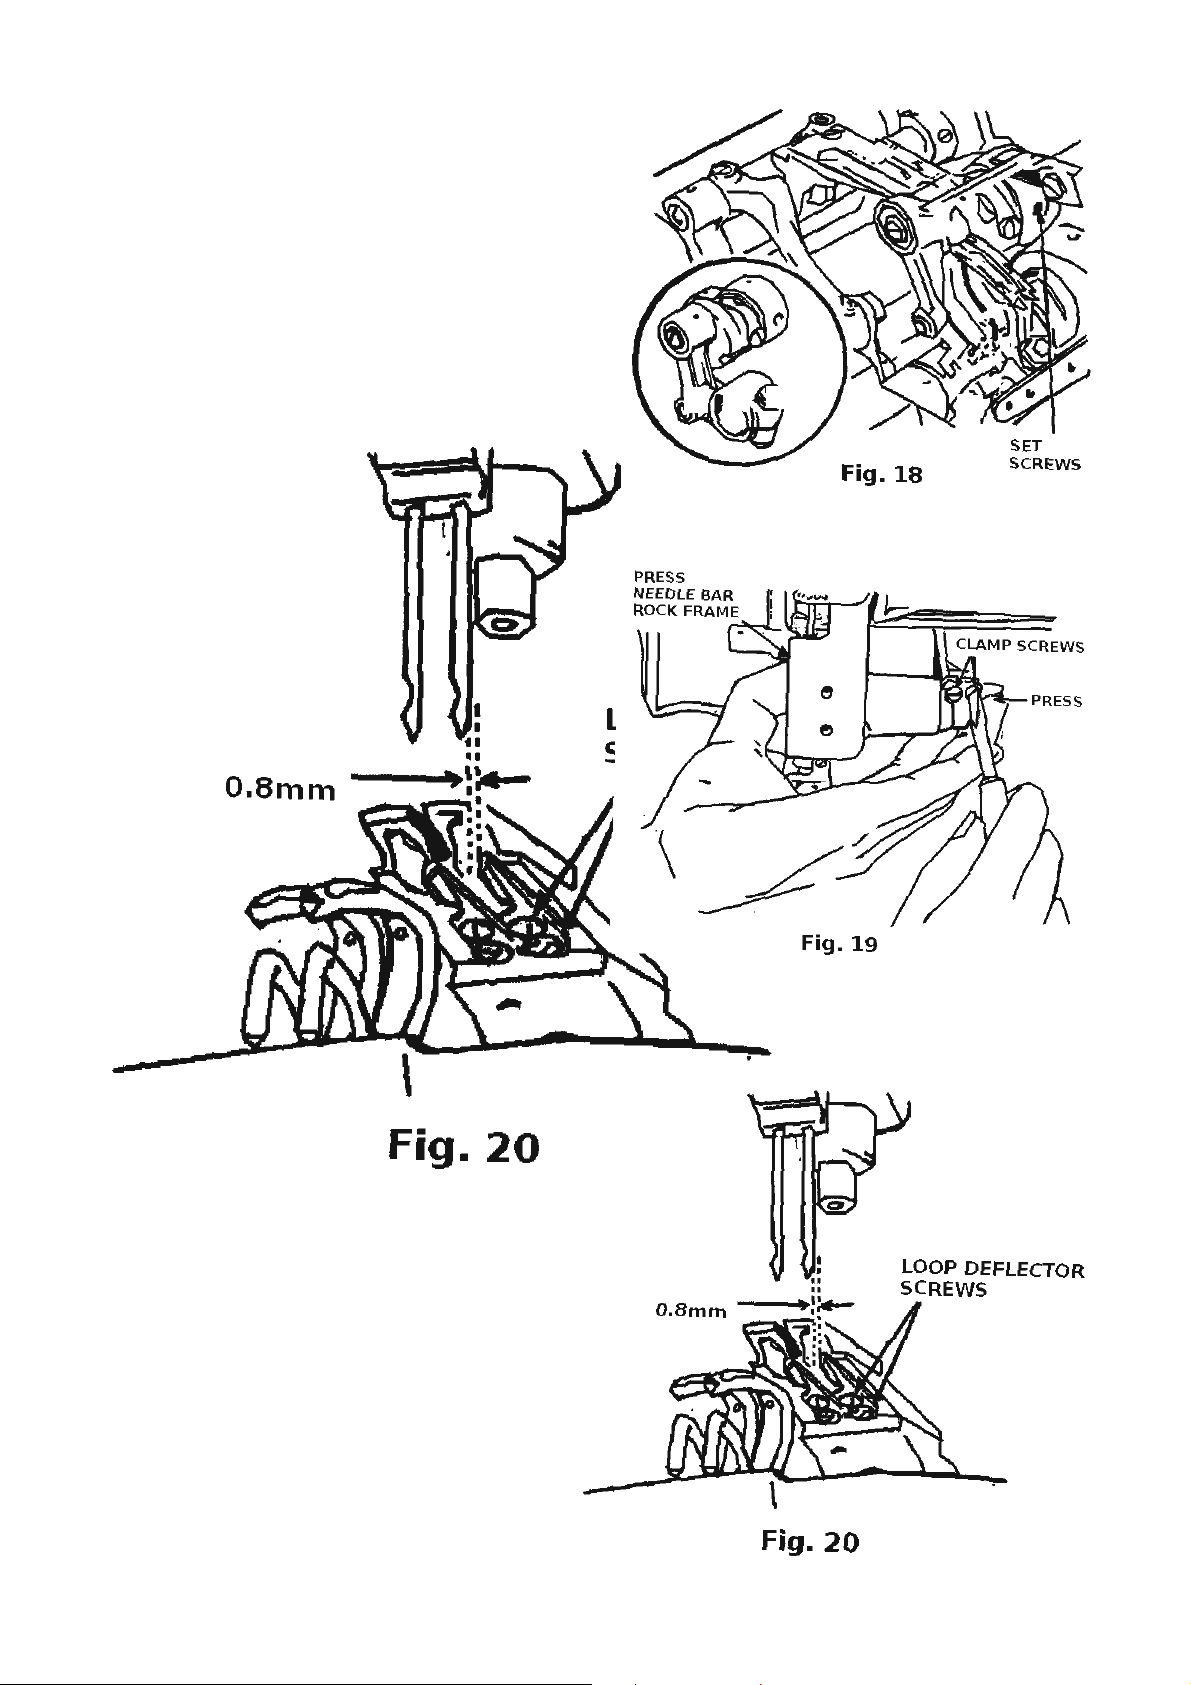
TIMING FEED LIFT ECCENTRIC
When the feed dog is at its highest
position, the top of the teeth should be
parallel with, and project full depth of teeth
above upper surface of throat plate. To
adjust, insert screwdriver in hole in feed
strap and loosen the two set screws,
Fig.18. Move feed lift eccentric forward for
earlier rise of feed dog, or backwards for
later rise. Then tighten the two set screws.
NEEDLE BAR POSITIONING
Needles should enter needle holes of
feed dog toward the front with
approximately the same clearance
between the front of the needle and the
needle holes as at the side. To adjust,
press needle bar rock frame, Fig.19,
against drive arm, and at the same time
loosen the two driving arm clamp screws.
Continue holding the rock frame against
the drive arm, move needle bar to correct
position and tighten the two clamp
screws.
POSITIONING LOOP DEFLECTORS
When loop deflector, located on
underside of feed dog, is positioned
correctly, there should be a clearance of
approximately 0.8 mm between the right
side of the needle and the loop deflector.
To adjust, move looper out of sewing
position and tilt machine back on its
hinges. Loosen loop deflector screws,
Fig.20. Move deflectors toward rear of feed
dog as far as the screw slots allow.
Tighten slightly to allow for further
adjustment. Return looper to sewing
position and turn machine pulley until
needle bar has descended to bottom of the
needle bar stroke. Tap deflector to left or
right until correct clearance is attained.
Move looper out of sewing position and
tighten loop deflector screws.
10
Page 12
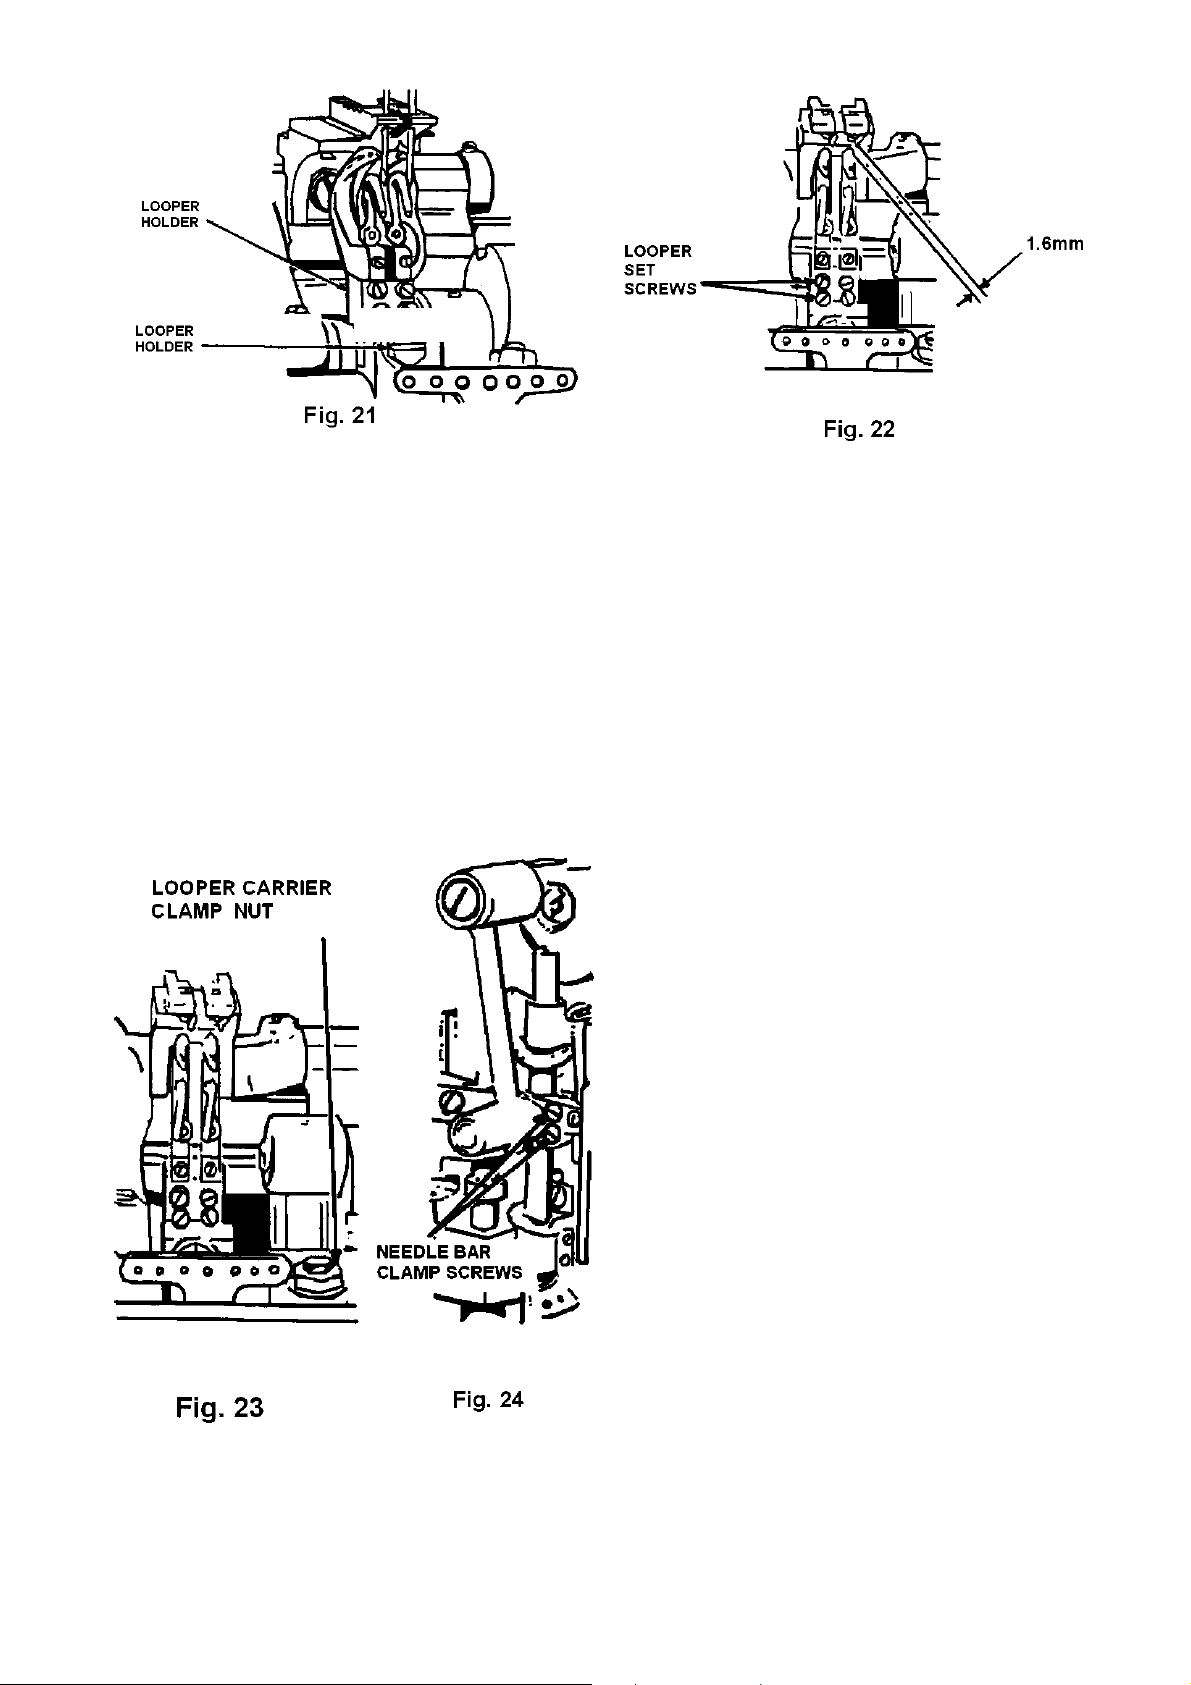
SETTING THE LOOPER AT CORRECT DISTANCE FROM NEEDLE
Sidewise Setting
When the looper is correctly
positioned, the point of the looper just
clears the scarf of the needle on the
forward stroke of the looper. To adjust,
turn machine pulley until the looper point
is directly apposide the center of the
needle. Loosen looper holder screw,
Fig.21, and tap holder to left or right until
correct clearance is attained. Then
securely tighten the looper holder screw.
Move looper to extreme forward
position. Check clearance between heel
of looper and loop deflector, Fig. 22,
which should be approximately 1.6 mm.
To adjust, loosen the two looper set
screws. Turn looper to left or right until
correct clearance is attained. Hold in
position and securely tighten the two
set screws.
CAUTION: On single and multiple
needle machines, make certain that the
point of each looper just clears the scarf
of its respective needle. To adjust, with
looper point directly opposite center of
needle, loosen the two set screws. Fig.
22, and turn looper slightly to left or
right. Then tighten the set screws.
Lengthwise Setting and Setting
Height of Needle Bar
When correctly set, the point of
the looper should be directly opposite
the center of the needle, and at the
center of the clearance above the eye of
the needle when the looper timing mark
LT on machine pulley is opposite the
timing arrow on the arm.
To adjust the looper, loosen looper
carrier clamping nut, Fig. 23. Move
carrier forward or backward until looper
point is directly opposite center of
needle. Then tighten clamping nut.
To adjust needle bar, first make
certain that needle is inserted up into
the needle bar or clamp as far as
possible. Loosen the two needle bar
clamping screws, Fig. 24, and raise or
lower needle bar to correct position.
Then securely tighten the two clamping
screws.
11
Page 13
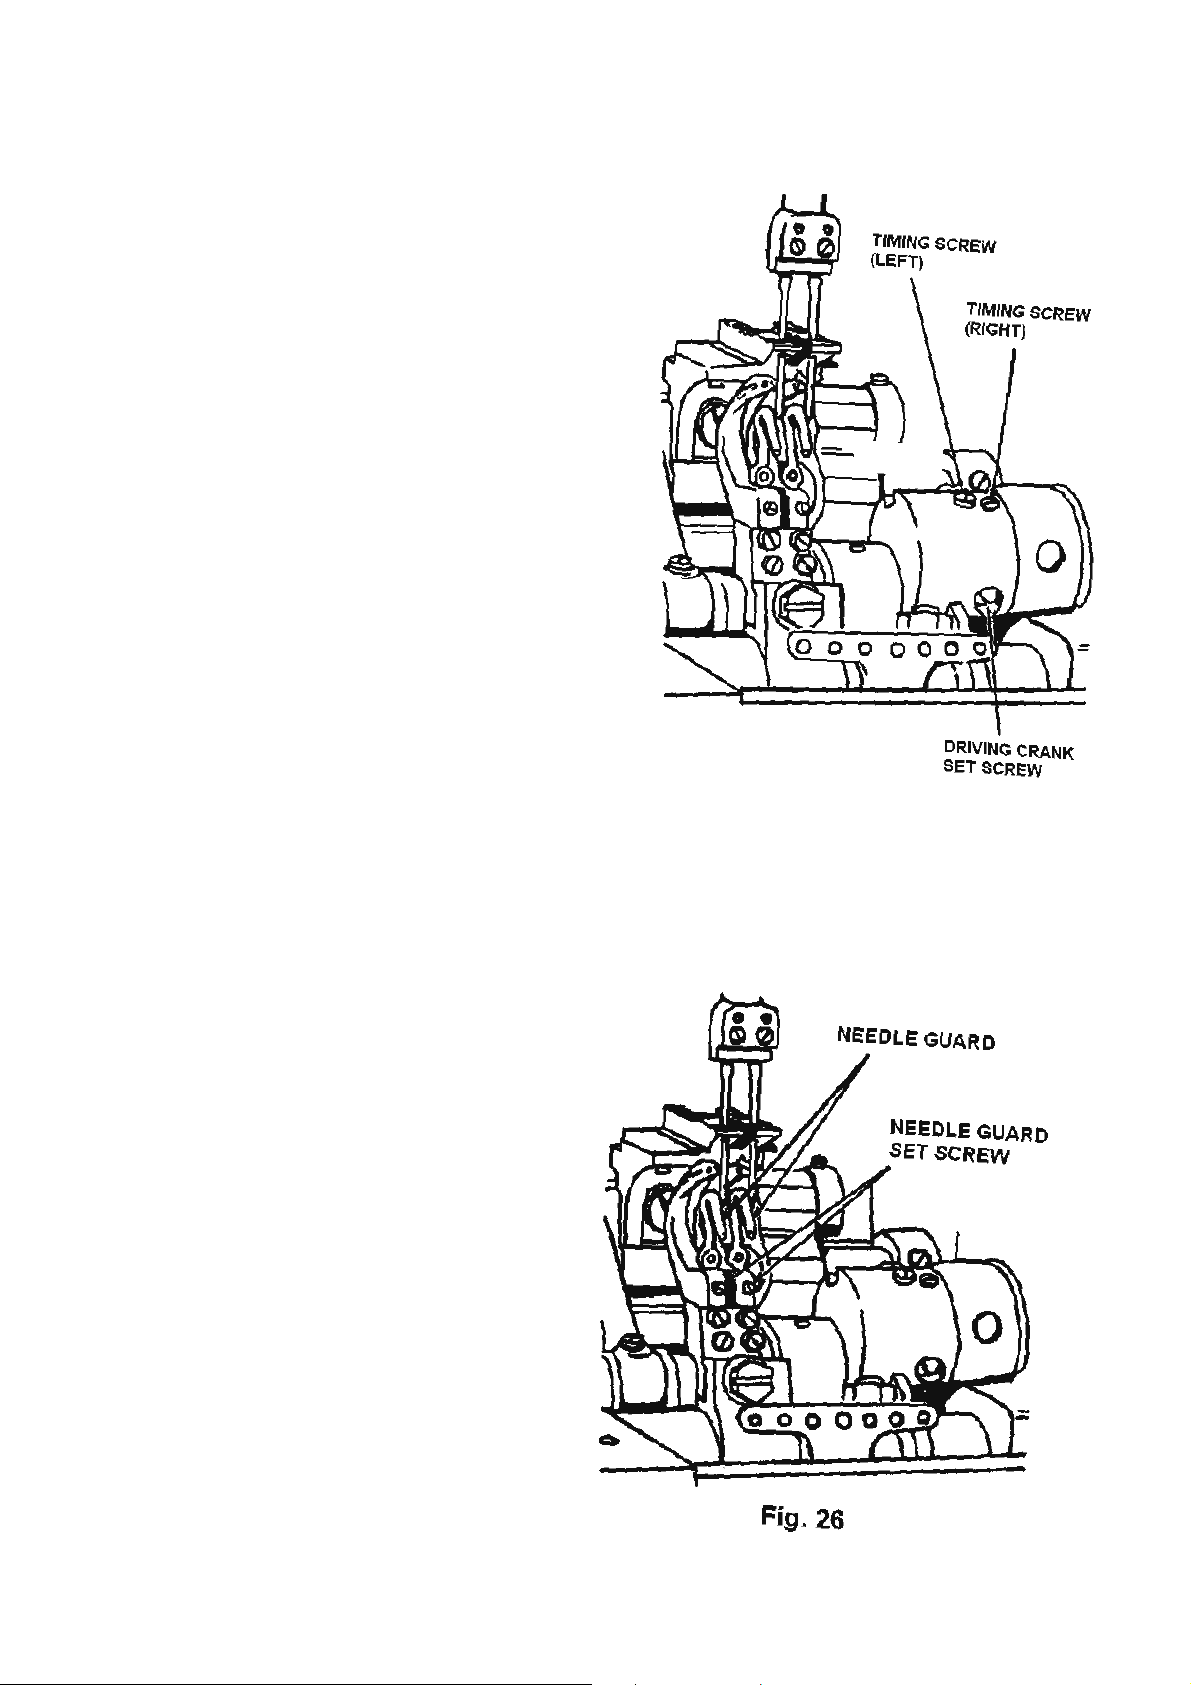
TIMING LOOPER DRIVING CRANK
When the looper driving crank is
properly timed, the point of the looper will
pass above the eye of the needle at the
same distance on both the forward and
backward strokes of the looper.
To adjust when point of looper
passes higher on forward stroke, loosen
looper driving crank set screw, Fig. 25.
Lossen looper crank timing screw (left)
approximately 1/8 turn, and tighten looper
crank timing screw (right). Continue to
adjust until correct adjustment is made.
Then securely tighten set screw.
When point of looper passes higher
on backward stroke, reverse the
adjustment by loosening timing screw
(right) and tightening timing screw (left).
SETTING THE NEEDLE GUARDS
When needle guards are properly set,
they should pass as close as possible to
the needles without touching. To adjust,
turn machine pulley over toward operator
until the points of the loopers are about to
pass the needle on their forward strokes.
At this point, the looper timing mark LT on
the machine pulley should be
approximately 3.2 mm above the arrow on
machine arm. Loosen needle guard set
screws, Fig. 26. Turn needle guards as
close to the needles as possible without
touching. Tighten set screws. Check by
springing the needle to the left and turning
the machine pulley to make certain that
the looper points do not stroke the needle.
12
Page 14
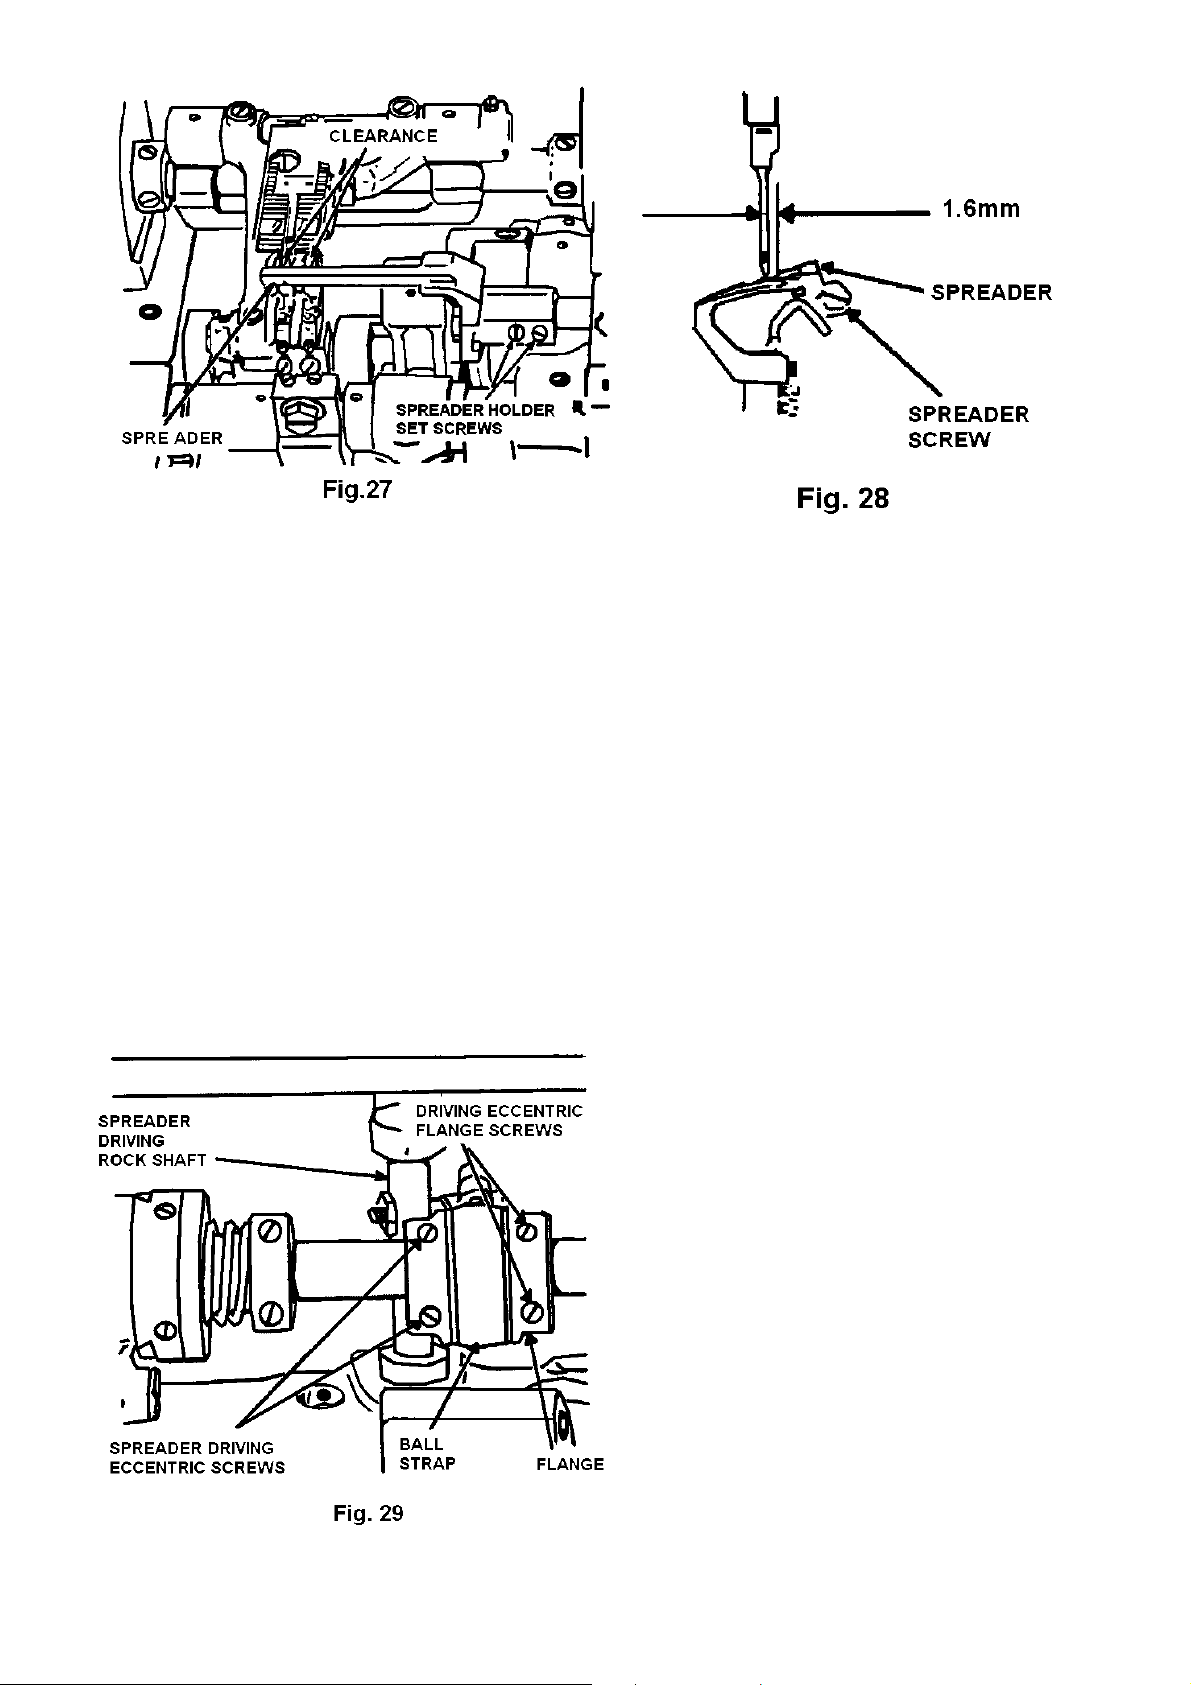
POSITIONING SPREADER
Sidewise and Height Setting
When looper on its forward stoke is
passing spreader……
The point of the spreader should be
exactly opposite top of thread
groove at left side of looper.
The clearance between spreader
point and looper should be
approximately the double thickness
of ordinary paper.
13
To adjust, loosen the two spreader
holder set screws. Fig. 27. Move
spreader and holder to correct position.
Hold in position and tighten the set
screws.
Lengthwise Setting
When the point of the needle on its
downward stroke is even with the point
of the spreader, the clearance between
the two points should be approximately
1.6 mm. To adjust, loosen spreader
screw. Fig. 28, and move spreader
forward or backward to correct position.
Then tighten spreader screw.
CHANGING MOVEMENT OF
SPREADER
The sidewise movement of the
spreader may be adjusted for sewing
under abnormal conditions. Under
normal conditions, maximum spreader
movement is generally used. To adjust,
tilt machine back on its hinges, loosen
the two spreader driving eccentric
screws, Fig. 29, and the two spreader
driving eccentric flange screws. Move
eccentric to left to increase movement,
or to right to decrease movement. When
correctly positioned, tighten the two
spreader driving eccentric screws first,
hold flange against strap and tighten
flange screws. Then refer to preceeding
information regarding positioning of
spreader.
CAUTION: When increasing
sidewise movement, allow sufficient
clearance between spreader driving
rock shaft, Fig. 29, and left side of
eccentric ball strap They should not
touch when eccentric ball stud is in its
highest position.
Page 15
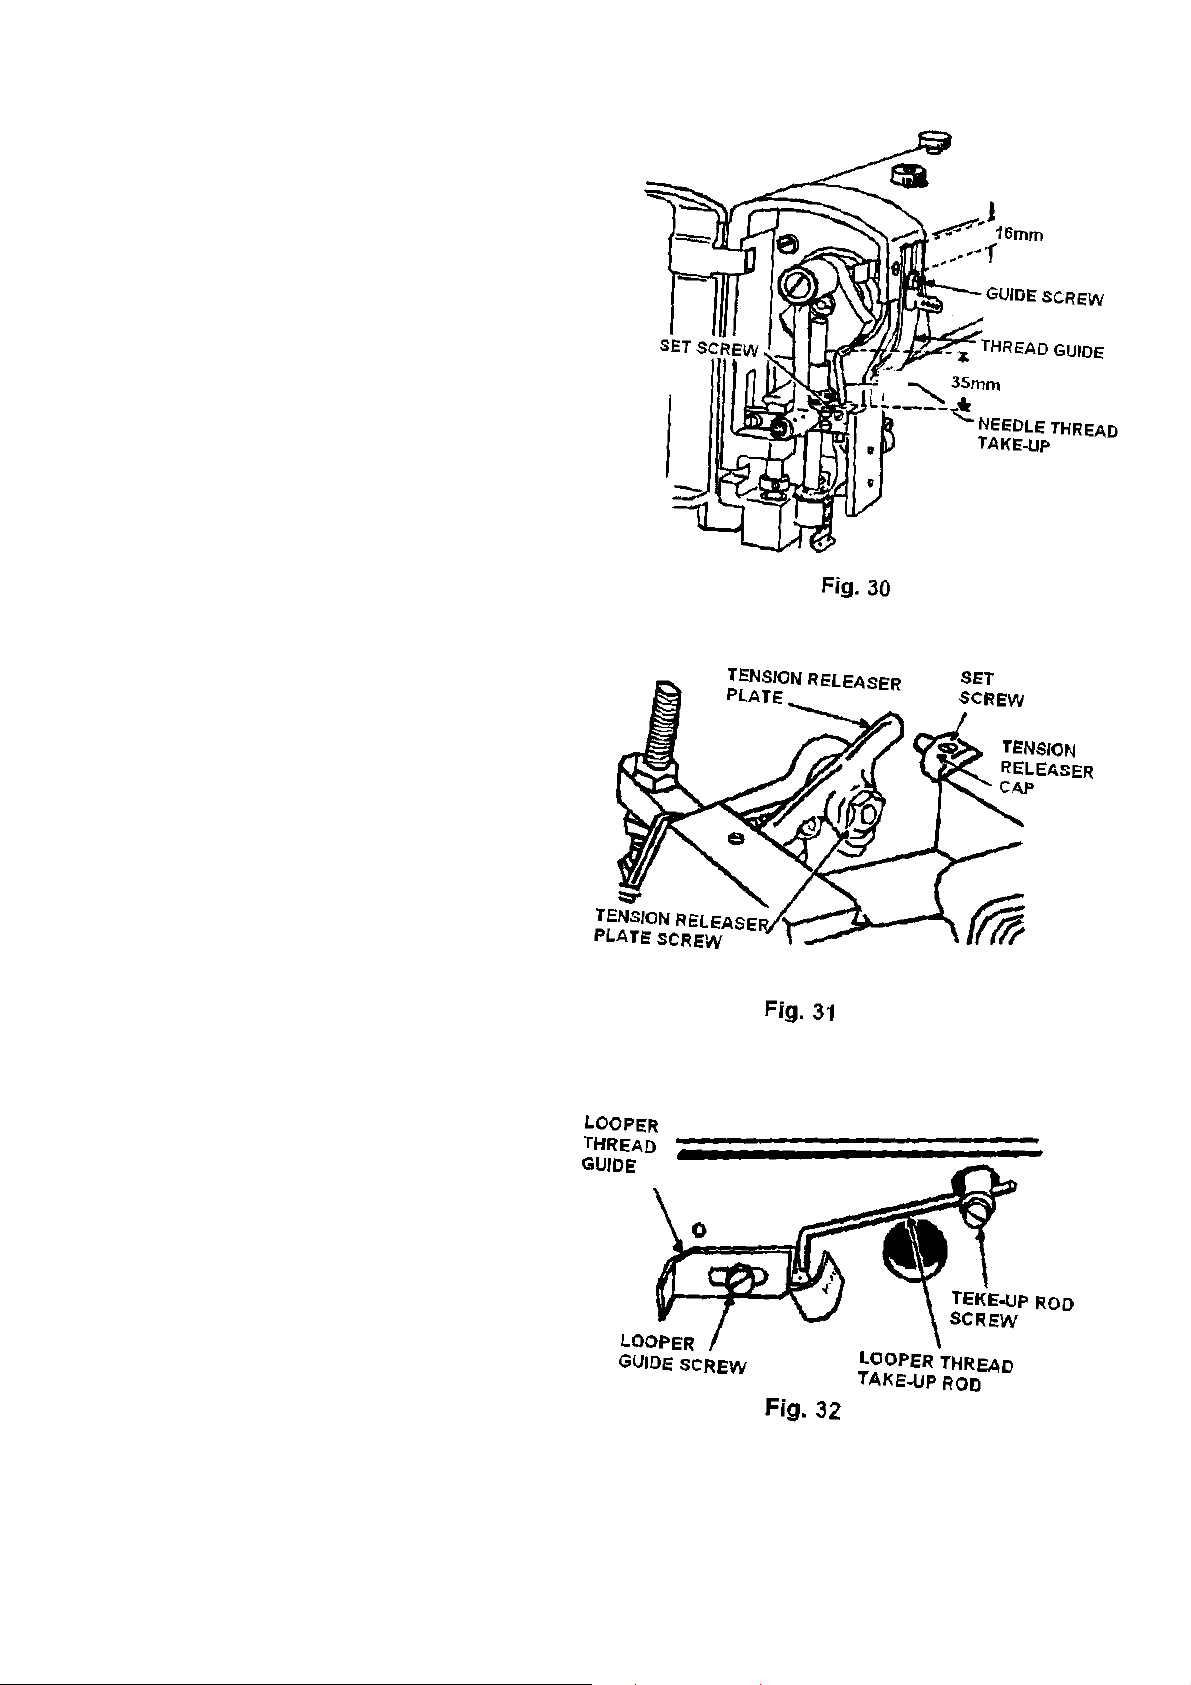
ADJUSTING NEEDLE THREAD
TAKE-UP
The needle thread take-up and thread
guide may be adjusted to increase or
decrease the amount of thread draw at the
top of the needle bar stroke. To increase
the amount, loosen thread take-up set
screw, Fig. 30, and raise take-up or loosen
guide screw and lower the guide. To
decrease the amount, reverse the
adjustment by lowering the take-up or
raising the guide.
For average sewing conditions the
guide should be set with upper end 16 mm
above the guide screw. The thread take-up
should be set with the lower end 35 mm
below the bottom of its holder.
ADJUSTING NEEDLE THREAD TENSION
RELEASER
When correctly adjusted, the tension
releaser should release tension on the
needle thread when the presser foot is
raised and allow full adjusted tension
when presser foot is down. To adjust,
loosen set screw, Fig. 31, and move
tension releaser cap out for earlier release
of tension or in for later release. Hold in
position and tighten set screw. Should the
tension releaser not release tension at the
correct time after making the above
adjustments, loosen the tension releaser
plate screw and move plate sidewise to
correct position. Then tighten screw.
ADJUSTING LOOPER THREAD TAKE-UP
The looper thread take-up and guide
may be adjusted for handling more or less
thread, according to thickness of material
and length of stitch, and to change the
ratio of looper thread in the finished stitch.
To change the amount of thread
hanled, loosen looper thread guide screw,
Fig. 32, looper thread take-up rod screw.
Move thread guide and take-up rod to the
left for more thread or to the right for less
thread. Tighten the two screws making
certain that take-up rod passes through
the center of the guide yoke.
To change ratio of looper thread in
finished stitch, loosen thread guide screw,
Fig. 32, and lower the yoke or right end of
thread guide for more thread. For less
thread, raise end of guide. Hold in position
and tighten guide screw.
14
Page 16
Page 17
Page 18
Page 19
Page 20
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
Page. 1
414504 1-1
141424 1-2
548035 1-3
504020 1-4
414509 1-5
414543 1-6
267617 1-7
268258 1-8
32788 1-9
414529 1-9-1
267110 1-10
415065 1-11
267633 1-12
415069 1-13
415071 1-14
544875 1-15
415458 1-16
414571 1-17
203941 1-18
267613 1-19
267614 1-20
267627 1-21
414548 1-22
267718 1-23
267093 1-24
544322 1-25
544301 1-26
543841-001 1-27
267907 1-28
267738 1-29
267731 1-30
1-31
267025 1-32
267626 1-33
415067 1-34
141338 1-35
414511 1-36
415061 1-37
545174-452 1-38
268330 1-39
415016 1-40
268032 1-41
268513 1-42
414514 1-43
414534 1-44
267658 1-45
267657 1-46
414516 1-47
414512 1-48
414530 1-49
415059 1-50
267628 1-51
267612 1-52
415041 1-53
415041 1-54
268512 1-55
268144 1-56
268278 1-57
414522 1-58
350604 1-59
415045 1-60
LIFTING ROCK SHAFT BRACKET SCREW
LIFTING LINK HINGE PIN SET SCREW
LIFTING ROCK SHAFT CRANK PIN
LIFTING ROCK SHAFT COLLAR SET SCREW
FOOT LIFTER ARM PINCH SCREW
LIFTING ECCENTRIC CONNECTION HINGE PIN PINCH SCREW
LIFTING LINK HINGE PIN WITH OIL WICK
LIFTING LINK HINGE PIN OIL PACKING
LIFTING ROCK SHAFT CRANK
SCREW
LIFTING ROCK SHAFT NEEDLE BEARING
LIFTING ROCK SHAFT COLLAR
LIFTING ROCK SHAFT
LIFTING ECCENTRIC CONNECTION CRANK
LIFTING ROCK SHAFT BRACKET
(NOT USE FOR TAKING TK-300U)
FOOT LEVER (FRONT) SPRING SCREW STUD
FOOT LIFTER LEVER (FRONT) SPRING
FOOT LIFTER LEVER (FRONT) WITH HINGE PIN
FOOT LIFTER LEVER (FRONT) HINGE PIN
LIFTING LINK
PRESSER BAR SPRING ARM BALL BEARING RETAINER SCREW
PRESSER BAR SPRING ARM BEARING RETAINER
LIFTING LEVER NEEDLE BEARING
LIFTING LEVER HINGE STUD SET SCREW
SCREW
LIFTING LOCK SHAFT BRACKET PIN
LIFTING PRESSER BAR GUIDE ROD
PRESSER BAR SPRING ARM
LIFTING PRESSER BAR LIFTING CRANK
PRESSER BAR SPRING ARM BALL BEARING
LIFTING LEVER HINGE STUD
LIFTING LEVER
LIFTING CRANK SET SCREW
NEEDLE BAR CONNECTING STUD PINCH SCREW
LIFTING CRANK
FACE PLATE HINGE STUD SET SCREW
FACE PLATE HINGE STUD
FACE PLATE LOCK SPRING PLATE
FACE PLATE LOCK SPRING
NEEDLE THREAD GUIDE
NEEDLE THREAD GUIDE SCREW
FACE PLATE LOCK SPRING SCREW
VIBRATING PRESSER BAR HINGE STUD
VIBRATING PRESSER BAR
LOOPER CARRIER CRANK HINGE PINCH SCREW
SCREW
LIFTING PRESSER BAR GUIDE ROD SET SCREW (LOWER)
LIFTING PRESSER BAR GUIDE BLOCK
LIFTING PRESSER BAR FOOT LIFTER CRANK
FOOT LIFTER CRANK
FOOT LIFTING CRANK STOP SCREW STUD
NEEDLE BAR
NEEDLE THREAD GUIDE
NEEDLE BAR OILING FELT
NEEDLE BAR OILING FELT HOLDER
NEEDLE BAR OILING FELT HOLDER SCREW
SCREW
NEEDLE BAR ROCK FRAME
1/8
Page 21
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
268029 1-61
268219 1-62
414539 1-63
415014 1-64
1-64-1
1-64-2
268033 1-65
268312 1-66
414517 1-67
267139 1-68
270266 1-69
268056 1-70
1-70-1
414638 1-71
267659 1-72
267632 1-73
202330 1-74
415053 1-75
414519 1-76
548005 1-77
267656 1-78
504019 1-79
236957 1-80
414519 1-81
228661 1-82
32827 1-83
414508 1-84
267664 1-85
267665 1-86
229 1-87
541200 1-88
414559 1-89
545489 1-90
415208 1-91
543804-004 1-92
414520 1-93
549024 1-94
500264-833 1-95
544204-001 1-96
268035 1-97
415297 1-98
268070 1-99
415200 1-100
415198 1-101
545213 1-102
415178 1-103
415026 1-104
415028 1-105
267970 1-106
549146 1-107
268022 1-108
415035 1-109
268081 1-110
270026 1-111
268082 1-112
545249-452 1-113
240245 1-114
415180 1-115
414515 1-116
268096 1-117
415034-451 1-118
415202 1-119
32789 1-120
NEEDLE BAR ROCK FRAME NEEDLE BEARING
NEEDLE BAR ROCK FRAME THREAD GUIDE
NEEDLE BAR ROCK FRAME THREAD GUIDE SCREW
FACE PLATE (FOR TK-300U-1/2/4)
FACE PLATE (FOR PORTER STYLE)
FACE PLATE (FOR TK-300U-1C/2C))
FACE PLATE LOCK STUD
NEEDLE THREAD GUIDE
NEEDLE BAR CONNECTING LINK CAP WASHER SCREW
NEEDLE BAR CONNECTING LINK CAP WASHER
NEEDLE BAR CONNECTING LINK BEARING
NEEDLE BAR CONNECTING LINK ASM
NEEDLE BAR CONNECTING LINK (SHORT) ASM
LIFTING PRESSER FOOT PINCH SCREW
VIBRATING PRESSER FOOT
LIFTING PRESSER FOOT
WICK
NEEDLE BAR CONNECTING STUD
SCREW
ARM HEAD POSITION PIN
THREAD LUBRICATOR
THREAD LUBRICATOR
LOOPER THREAD TAKE-UP ROD SET SCREW
THREAD LUBRICATOR OIL PAD
FEED PLATE CUSHION (NEOPRENE)
THROAT PLATE
BED PLATE SCREW
FEED DOG
LOOPER DEFLECTOR
LOOPER DEFLECTOR SCREW
FEED DOG ADJUSTING SCREW NUT
FEED DOG ADJUSTING SCREW
NUT
FEED DOG SHANK
WASHER
FEED DOG SHANK SCREW
FEED DRIVING ROCK FRAME POSITION SCREW
LOOPER DRIVING CRANK SET SCREW
SCREW
FEED BAR HINGE PIN
ROLLER
FEED DRIVING ROCK SHAFT
FEED DRIVING ROCK FRAME
FEED BAR
SCREW
LOOPER THROW-OUT RACK ROD WITH THUMB NUT
BED PLATE (LEFT)
BED PLATE SLIDE
BED PLATE SLIDE SPRIG
SCREW
BED PLATE SLIDE SPRING
BED PLATE
FEED REGULATING STUD
SPRING
FEED REGULATING STUD SOCKET
FEED REGULATING STUD SOCKET SCREW
FEED REGULATING RETAINING SPRING
LOOPER THROW-OUT GEAR
SCREW
LOOPER CARRIER SHAFT BUSHING POSITION PLATE
BED PLATE ASM
FEED BAR HINGE PIN COLLAR
LIFTING ROCK SHAFT CRANK & PIN
2/8
Page 22
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
415179 1-121
LOOPER THROW-OUT RACK ROD
3/8
Page 23
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
541451 1-122
415027 1-123
414545 1-135
LOOPER THROW-OUT RACK ROD THUMB NUT
BED PLATE SLIDE COMPLETE
NEEDLE THREAD GUIDE SET SCREW
Page. 2
268505 2-1
50169 2-2
268111 2-3
414537 2-4
268506 2-5
502986 2-6
248423 2-7
268615 2-8
544336 2-9
204348 2-10
414570 2-11
414577 2-12
LOOPER THREAD GUIDE
LOOPER THREAD GUIDE BRACKET SCREW
LOOPER THREAD GUIDE BRACKET
LOOPER THREAD GUIDE BRAKCET SCREW
THREAD GUIDE
SCREW
FOOT LIFTER ROD COTTER PIN
FOOT LIFTING LEVER ROD
FOOT LIFTER LEVER SPRING SCREW
FOOT LIFTING LEVER SPRING
FOOT LIFTER LEVER SPRING SCREW EYE
FOOT LIFTER EVER ROD HINGE SCREW
2-13
541166-003 2-14
567646 2-15
201363(803) 2-16
415104 2-17
267171 2-18
543850-001 2-19
415120 2-20
FOOT LIFTER LEVER ROD HINGE SCREW NUT
PRESSER BAR SPRING ARM FULCRUM
FOOT LIFTER LEVER HINGE SCREW
FOOT LIFTER LEVER
NEEDLE THREAD TENSION RELEASING PLATE
NEEDLE THREAD TENSION RELEASING PLATE PIN
FOOT LIFTER ARM
2-21
544358 2-22
244084 2-23
415111 2-24
414579 2-25
541198 2-26
414523 2-27
548459 2-28
415107 2-29
415106 2-30A
415116 2-30C
2-30B
415115 2-31
267655 2-32
415114 2-33
267641 2-34
415109 2-35
267653 2-36
267645 2-37
415113 2-38
414567 2-39
548154 2-40
545405 2-41
545205-451 2-42
267650 2-43
415098 2-44
414527 2-45
415099 2-46
414528 2-47
268419 2-48
268148 2-49
214529 2-50
545297 2-51
415092 2-52
541197 2-53
268061 2-54
268060 2-55
415368 2-56
SCREW
SCREW
PRESSER BAR PRESSURE CYLINDER SUPPORT
PRESSER BAR PRESSURE CYLINDER SUPPORT STUD
NUT
SCREW
WASHER
PRESSER BAR SPRING BOUSING ASM
PRESSER BAR SPRING BOUSING COMPLETE (SMALL)
PRESSER BAR SPRING BUSHING COMPLETE (LARGE)
PRESSER BAR SPRING BUSHING COMPLETE (MIDIUM)
NUT
WASHER
PLUNGER
WASHER
SPRING
NUT
WASHER (NYLON)
PRESSER BAR SPRING ARM FORK
PRESSER BAR SPRING ARM HINGE SCREW
WASHER
NUT
SCREW
PRESSER BAR PRESSURE CYLINDER SUPPORT RETAINER
NEEDLE BAR ROCK FRAME REGULATING STUD COMPLETE
SCREW
NEEDLE BAR ROCK FRAME REGULATING STUD CAP
SCREW
REGULATING STUD SLEEVE
NEEDLE BAR ROCK FRAME REGULATING STUD
REGULATING STUD SPRING
FEED DRIVING CONNECTION CAP SCREW
FEED LIFTING CONNECTION HINGE STUD
NUT
NEEDLE BAR ROCK FRAME DRIVING CONNECTION & BEARING
NEEDLE BAR ROCK FRAME DRIVING CONNECTION
FEED DRIVING CONNECTION NEEDLE BEARING
4/8
Page 24
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
415094 2-57
414790 2-58
2-59
415308 2-60
414529 2-61
504048 2-62
415252 2-63
415357 2-64
204365 2-65
268121 2-66
268167 2-67
545246-452 2-68
545246-452 2-68
267604 2-69
Cat. 4112-01 2-70
268382 2-71
141478 2-72
268380 2-73
141494 2-74
268310 2-75
268162 2-76
268638 2-77
414552 2-78
547670 2-79
415196 2-80
414524 2-81
268499 2-82
268190 2-83
268184 2-84
268079 2-85
268078 2-86
268131 2-87
41506 2-88
267933 2-89
415204 2-90
414501 2-91
543801-012 2-92
414549 2-93
414553 2-94
414558 2-95
417056 2-96
415167 2-97
415168 2-98
268132 2-99
268133 2-100
545205-451 2-101
268093 2-102
268368 2-103
268099 2-104
268208 2-105
268216 2-106
415292 2-107
415174 2-108
545424 2-109
415192 2-110
415194 2-111
414575 2-112
32825 2-113
268052 2-114
268051 2-115
414510 2-116
415170 2-117
414556 2-118
NEEDLE BAR ROCK FRAME DRIVING ARM
SCREW
LIFTING ECCENTRIC SPACING COLLAR
SCREW
SCREW
NEEDLE THREAD TENSION RELEASER CAP
NEEDLE THREAD TENSION RELEASER
NEEDLE THREAD TENSION RELEASER SPRING
TENSION BRACKET SPACING COLLAR
NEEDLE THREAD TENSION BRACKET
ARM SIDE COVER SCREW
SCREW
ARM SIDE COVER
NEEDLE
LOOPER AND NEEDLE GUARD COMPLETE
NEEDLE GUARD SET SCREW
LOOPER
SCREW
NEEDLE GUARD
SPREADER POINT
SPREADER
SPREADER SCREW
SPREADER WASHER
SPREADER HOLDER
SCREW
SPREADER BAR
SPREADER DRIVING PIN
SPREADER BAR BRACKET
FEED LIFTING LINK HINGE PIN
FEED LIFTING LINK
LOOPER THROW-OUT SAFETY LATCH
FEED LIFTING ROCK SHAFT CRANK
FEED LIFTING ROCK SHAFT
FEED LIFTING CRANK
SCREW
LOOPER THROW-OUT SAFETY LATCH RETAINING RING
SCREW
LOOPER HOLDER SCREW
SCREW
LOOPER HOLDER ASM
LOOPER CARRIER SHAFT & BUSHING
LOOPER CARRIER SHAFT BUSHING
LOOPER THROW-OUT SAFETY LATCH SPRING
LOOPER THROW-OUT SAFETY LATCH SPRING BRACKET
SCREW
LOOPER CARRIER SHAFT
LOOPER CARRIER
LOOPER DRIVING CONNECTION BUSHING
LOOPER CARRIER CRANK HINGE PIN
LOOPER DRIVING CONNECTION ASM
LOOPER CARRIER CRANK CLAMPING STUD
LOOPER CARRIER CRANK
NUT
SPREADER DRIVING ROCK SHAFT
SPREADER DRIVING CRANK
SPREADER DRIVIING ROCK SHAFT SCREW STUD
SPREADER DRIVING ROCK SHAFT SCREW STUD OIL PACKING
LOOPER THREAD TAKE-UP ROD
LOOPER THREAD GUIDE
SCREW
LOOPER CARRIER SHAFT BUSHING
LOOPER THREAD GUIDE SCREW
5/8
Page 25
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
268373 2-119
414564 2-120
415182 2-121
250265 2-122
201477 2-123
268313 2-124
541453 2-125
2-127
2-128
Page. 3
415075 3-1
LOOPER THREAD GUIDE
LOOPER THROW-OUT GEAR LOCKING PLANGER STOP SCREW
LOOPER THROW-OUT GEAR LOCKING PLUNGER
LOOPER THROW-OUT GEAR LOCKING PLUNGER SPRIN
LOOPERTHROW-OUT GEAR LOCKING PLUNGER SCREW BUHSING
LOOPER THROW-OUT GEAR LOCKING PLUNGER HANDLE
NUT
LIFTING ECCENTRIC AND NEEDLE BAR DRIVING ECCENTRIC COMPLETE
415078 3-2
268064 3-3
414557 3-4
241763 3-5
414555 3-6
415079 3-7
267623 3-8
374098 3-9
268065 3-10
267618 3-11
415077 3-12
544286 3-13
415077 3-14
268492 3-15
268493 3-16
415086 3-17
3-18
544208-005 3-19
414578 3-20
268214 3-21
268009 3-22
500272-833 3-23
415132 3-24
415133 3-25
32848 3-26
281206 3-27
415128 3-28
268264 3-29
415157 3-30
202253 3-31
414546 3-32
268004 3-33
268044 3-34
268270 3-35
226206 3-36
54279 3-37
267971 3-38
59539 3-39
50326 3-40
54570 3-41
2102 3-42
32572 3-43
59538 3-44
131741 3-45
143657 3-46
143658 3-47
415176 3-48
410536 3-49
374099 3-50
NEEDLE BAR ROCK FRAME DRIVING ECCENTRIC FLANGE
FEED DRIVING ECCENTRIC Φ28-57MM
SCREW
SET SCREW PACKING
SCREW
NEEDLE BAR ROCK FRAME DRIVING ECCENTRIC FLANGE
FEED DRIVING ECCENTRIC FRICTION PLATE
FEED DRIVING ECCENTRIC FRICTION PLATE SCREW
FEED DRIVING ECCENTRIC ADJUSTING DISC
LIFTING ECCENTRIC ADJUSTING DISC SPRING
LIFTING ECCENTRIC FRANGE
SCREW
LIFTING ECCENTRIC FLANGE
LIFTING ECCENTRIC CONNECTION
LIFTING ECCENTRIC CONNECTION WITH BEARING Φ28-57MM
LIFTING ECCENTRIC SPACING COLLAR
COLLAR & SCREW
SCREW
SCREW
BED SHAFT OIL STOP BALL SCREW
ARM SHAFT OIL STOP BALL SPRING
SCREW
NEEDLE BAR CRANK
NEEDLE BAR CRANK
ARM SHAFT BALL BEARING
NEEDLE BAR CRANK COVER
ARM SHAFT
ARM SHAFT OIL CONTROL ROD
ARM SHAFT CONNECTION BELT PULLEY
ARM SHAFT CONNECTION BELT PULLEY SPRING FLANGE
SCREW
ARM SHAFT BALL BEARING HOUSING
SPRING
ARM SHAFT CONNECTION BELT
NEEDLE THREAD TENSION RELEASING PIN
NEEDLE THREAD TENSION THREAD GUIDE
NEEDLE THREAD TENSION COMPLETE
NEEDLE THREAD TENSION STUD WITH THUMB NUT
NEEDLE THREAD TENSION STUD
NEEDLE THREAD TENSION THUMB NUT
TENSION DISC
NEEDLE THREAD TENSION RELEASING DISC
TENSION SPRING BUSHING
NEEDLE THREAD TENSION SPRING
NEEDLE THREAD TENSION SPRING BUSHING
NEEDLE THREAD TENSION THUMB NUT LOCKING SPRING
LOOPER DRIVIING CRANK
LOOPER DRIVING CRANK OIL STOP SCREW
LOOPER DRIVING CRANK POSITION SCREW
6/8
Page 26
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
545103 3-50
374099 3-50
414563 3-51
268102 3-52
204925 3-53
415210 3-54
268077 3-55
268074 3-56
415145 3-57
268265 3-58
268029 3-59
268029 3-60
415160 3-61
272140 3-62
415159 3-63
415091 3-64
415213 3-65
415072 3-66
415073 3-67
415074 3-68
268066 3-69
412011 3-70
544325 3-71
415183 3-72
3-72-1
415569 3-73
351876 3-74
268220 3-75
543808-002 3-76
415187 3-77
415361 3-78
543804-007 3-79
414532 3-80
415255 3-81
415295 3-82
268333 3-83
415294 3-84
415291 3-85
412203 3-86
10148 3-87
541452 3-88
228448 3-89
415350 3-90
415212 3-91
415190 3-92
3-93
415368 3-94
544336 3-95
3-101
3-102
3-103
3-106
268121 3-112
SCREW
LOOPER DRIVING CRANK POSITION SCREW
SCREW
LOOPER DRIVING CRANK OIL HOLE COVER
SPREADER SCREW WASHER
FEED LIFTING ECCENTRIC
FEED LIFTING ECCENTRIC LUBRICATING PAD
FEED LIFTING CONNECTION
BED SHAFT
BED SHAFT OIL CONTROL ROD
NEEDE BEARING
NEEDLE BEARING
BED SHAFT CONNECTING BELT PULLEY
ARM SHAFT BALL BEARING (BACK)
BED SHAFT CONNECTION BELT PULLEY WITH BEARING
NEEDLE BAR ROCK FRAME DRIVING CONNECTION HINGE STUD
FEED DRIVING ROCK SHAFT CRANK
FEED DRIVING ECCENTRIC COMPLETE
FEED DRIVING FLANGE ASM
FEED DRIVING FLANGE
ECCENTRIC ADJUSTING DISC SPRING
FEED LIFTING ECCENTRIC
SCREW
SPREADER DRIVING CONNECTION WITH BEARRING & BALL ROLLER
BEARING
SCREW
SPREADER DRIVING ROCK SHAFT SCREW STUD BALL ROLLER
SPREADER DRIVING ECCENTRIC THRUST WASHER
SCREW
SPREADER DRIVING ECCENTRIC
ARM SCREW
ARM SCREW WASHER
SCREW
LOOPER THREAD TENSION BRACKET
ARM POSITION PIN
LOOPER THREAD TENDION THREAD GUIDE
LOOPER THREAD TENSION COMPLETE
LOOPER THREAD TENSION STUD
LOOPER THREAD TENSION DISC
LOOPER THREAD TENSION SPRING
LOOPER THREAD TENSION THUMB NUT
MACHINE LOCATING STUD
LOOPER DRIVING CRANK ASM
FEED DRIVING CRANK & NEEDLE BAR DRIVING CONNECTION
SPREADER DRIVING ECCENTRIC COUNTER BLALANCE
SCREW
FEED DRIVING CONNECTION NEEDLE BEARING
SCREW
SCREW
SCREW
WASHER
Page. 4
415153-451 4-1
414526 4-2
414525 4-3
415154 4-4
415342 4-5
414639 4-6
268500 4-7
268123 4-8
MACHINE PULLEY
SCREW
SCREW
MACHINE PULLEY
BED SHAFT BALL BEARING
SCREW
LOOPER THREAD GUIDE GASKET
LOOPER THREAD TUBE
7/8
Page 27
TK-300W PARTS DESCRIPTION
Singer code Part No. Description
415009 4-12
BELL CASTING FRONT FACE
8/8
Page 28
大慶縫衣機械股份有限公司
TA KING INDUSTRIAL CO., LTD
8F, No. 230, Sec. 3, Cheng Teh Road,
P. O. Box 21~41, Taipei, Taiwan
E-mail: [email protected]
Tel: 886-2-25950288 Fax:886-2-25919233
 Loading...