

Page 1
READ THIS FIRST
MODEL SB1108
***IMPORTANT UPDATE***
SINCE
1906
Applies to Models Mfd. Since 06/23
and Owner’s Manual Printed 12/20
The following changes were recently made since the owner’s manual was printed:
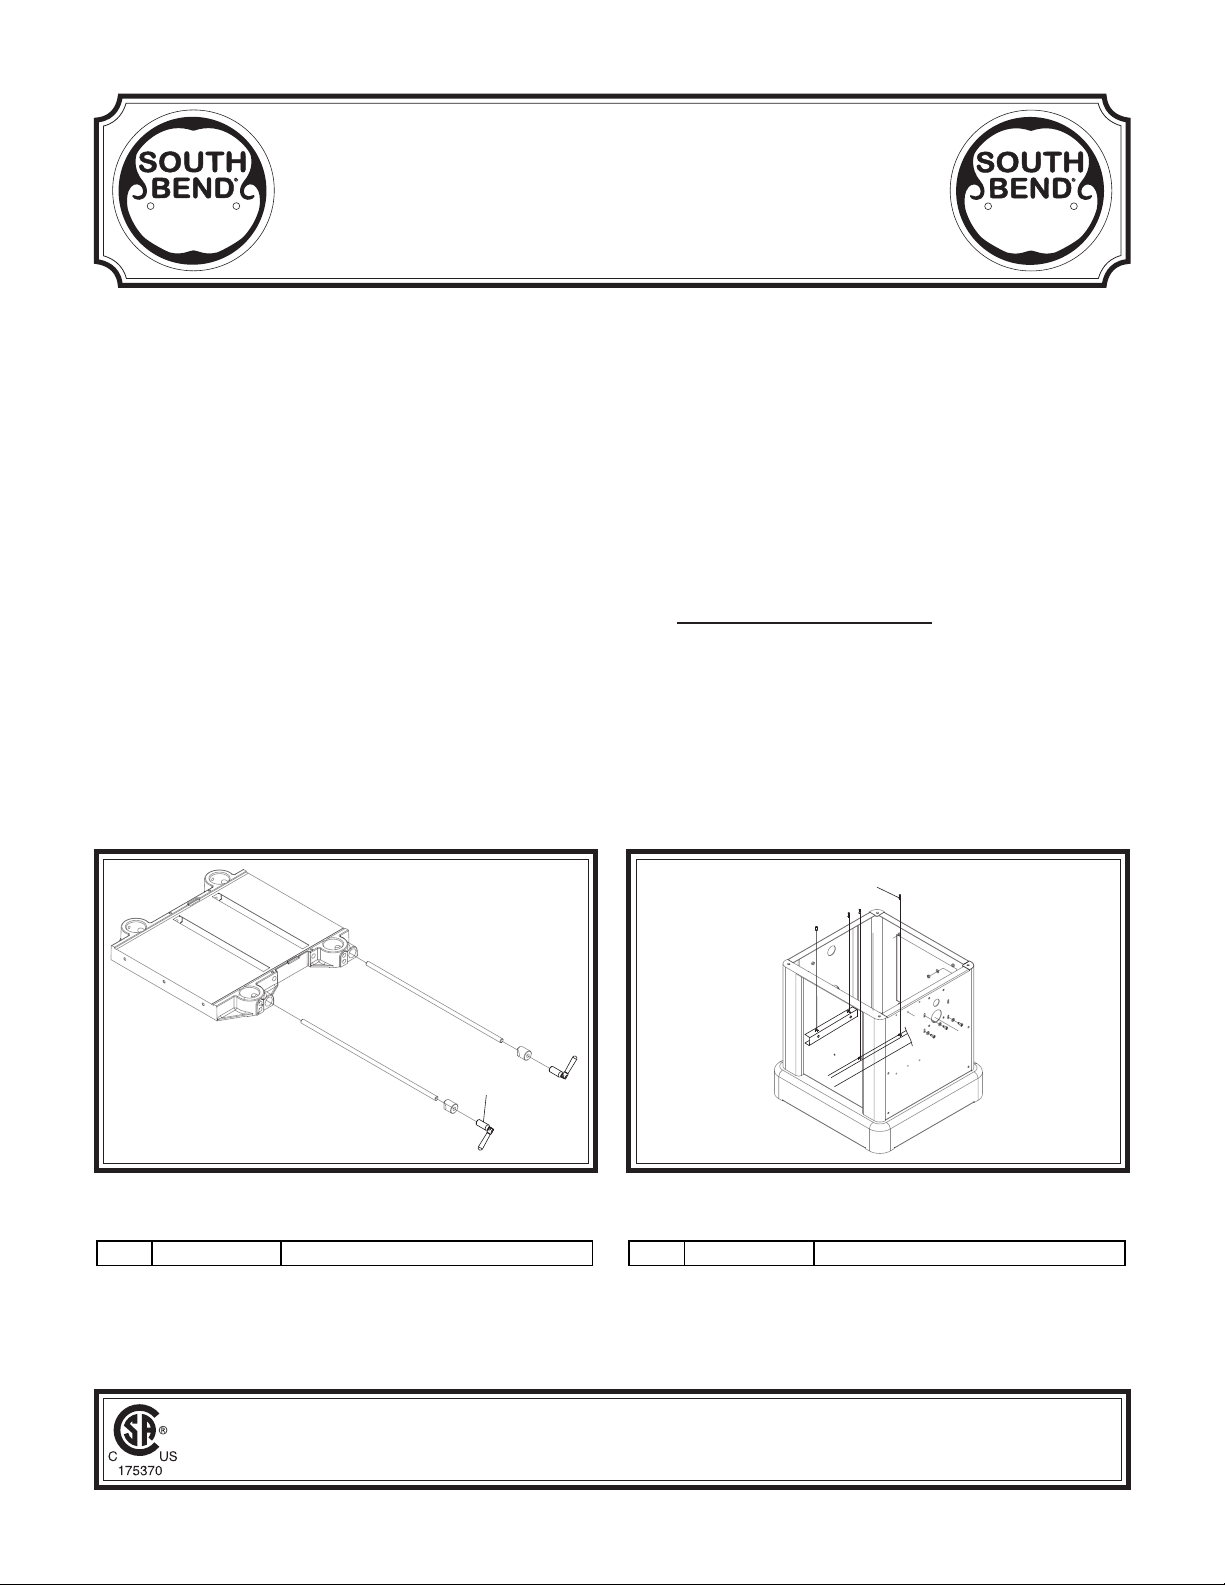
• Table lock knobs changed to lock handles.
• Two set screws added to stand.
• Spec for minimum stock thickness changed.
Aside from this information, all other content in the owner’s manual applies and MUST be read and
understood for your own safety. IMPORTANT: Keep this update with the owner’s manual for
future reference.
If you have any further questions about this manual update or the changes made to the machine,
contact our Technical Support at (360) 734-1540 or email www.southbendtools.com.
SINCE
1906
Revised Specifications
Main Specifications
Main Specifications
Min. Stock Thickness ............................................................................................................................................ 1/8 in.
Revised Table Parts
125V2
REFPART #
125V2 PSB1108125V2 PIVOT HANDLE M12-1.75 V2.06.23
DESCRIPTION
Revised Stand Parts
212V2
REFPART #
212V2 PSB1108212V2 SET SCREW M6-1 X 20 V2.07.23
DESCRIPTION
Copyright © August, 2023 by South Bend Tools
WARNING: No portion of this manual may be reproduced without written approval.
#LW22872 Printed in Taiwan
Page 2
READ THIS FIRST
REF PART # DESCRIPTION
REF PART # DESCRIPTION
MODEL SB1108/SB1109
***IMPORTANT UPDATE***
SINCE
1906
Applies to Models Mfd. Since 11/22
and Owner’s Manual Printed 12/20
The following change was made to this machine since the owner’s manual was printed:
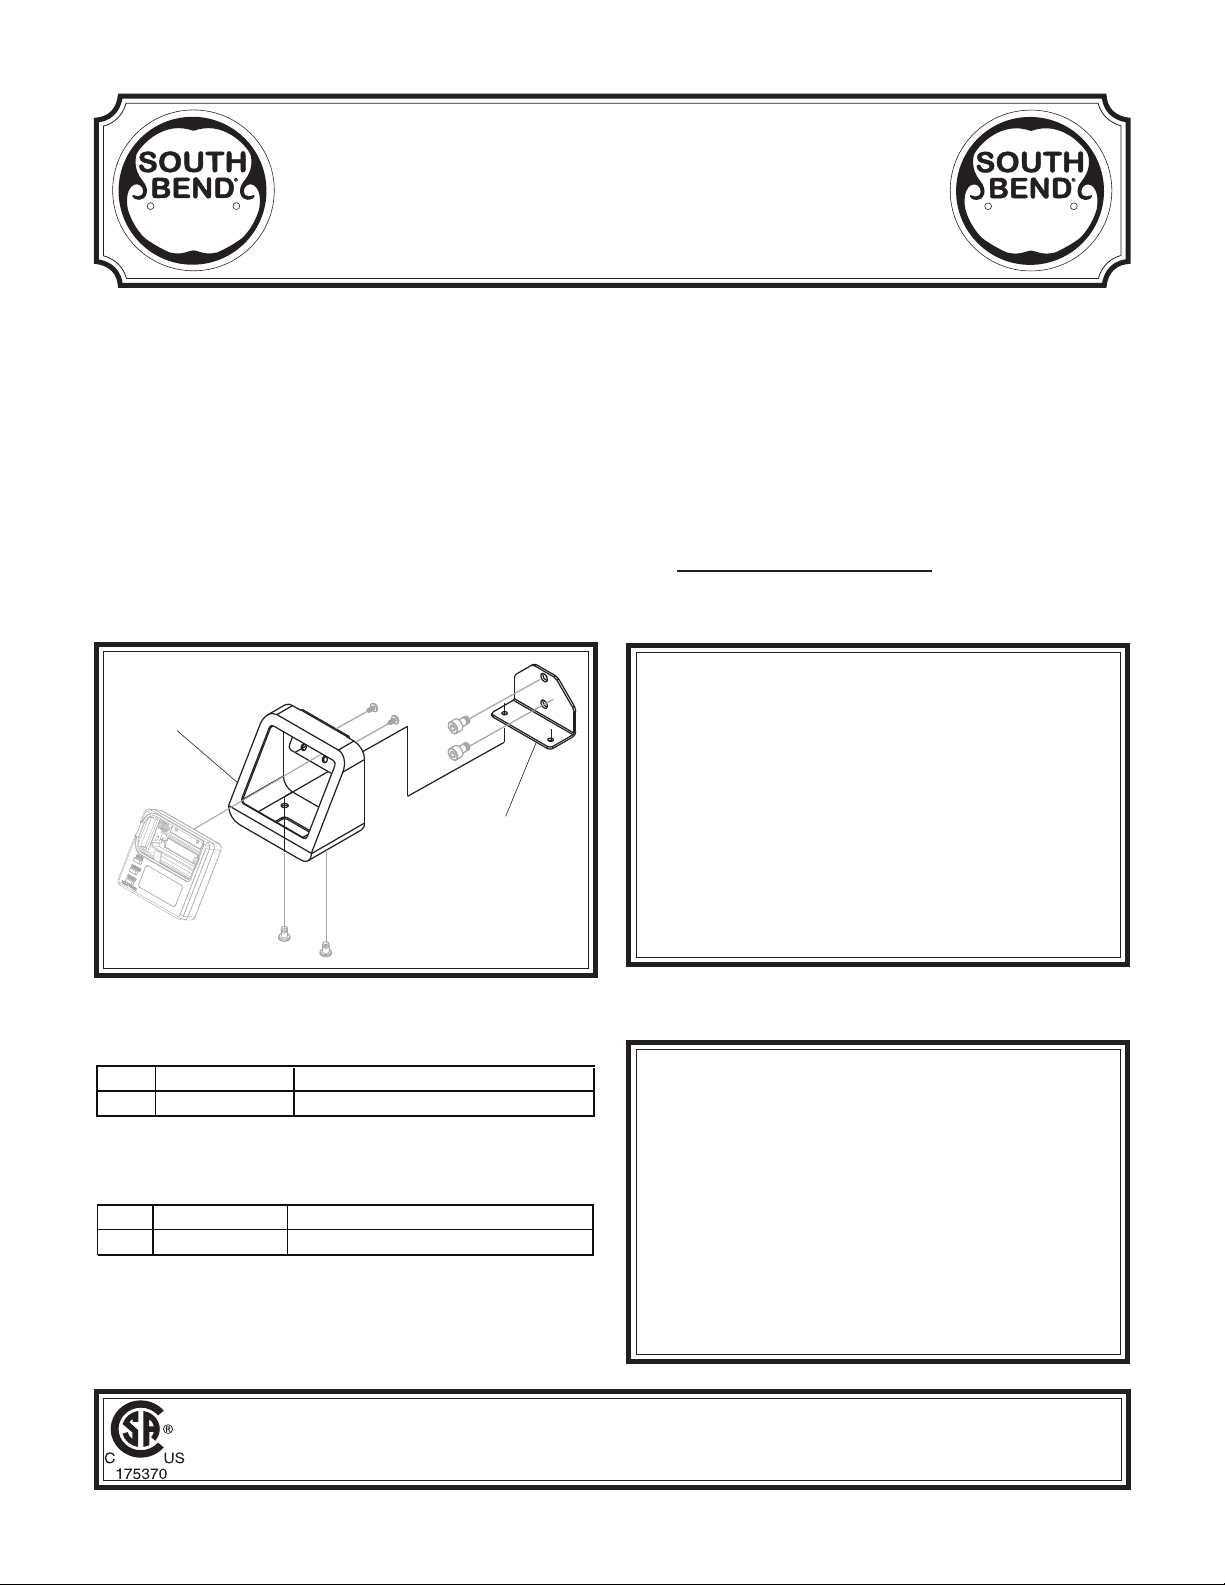
• Digital readout bracket and housing changed.
Aside from this information, all other content in the owner’s manual applies and MUST be read and
understood for your own safety. IMPORTANT: Keep this update with the owner’s manual for
future reference.
If you have any further questions about this manual update or the changes made to the machine,
contact our Technical Support at (360) 734-1540 or email www.southbendtools.com.
SINCE
1906
Revised Parts
63V2 (SB1108)
52V2 (SB1109)
SB1108
61V2 PSB1108061V2
63V2 PSB1108063V2
SB1109
Old DRO Housing
61V2 (SB1108)
51V2 (SB1109)
New DRO Housing
DIGITAL READOUT BRACKET V2.11.22
DIGITAL READOUT HOUSING V2.11.22
51V2 PSB1109051V2
52V2 PSB1109052V2
WARNING: No portion of this manual may be reproduced without written approval.
DIGITAL READOUT BRACKET V2.11.22
DIGITAL READOUT HOUSING V2.11.22
Copyright © September, 2022 by South Bend Tools
#JP22475 Printed in Taiwan
Page 3
READ THIS FIRST
MODEL SB1108/SB1109
***IMPORTANT UPDATE***
SINCE
1906
Applies to Models Mfd. Since 07/22
and Owner’s Manual Printed 12/20
The following change was made to this machine since the owner’s manual was printed:
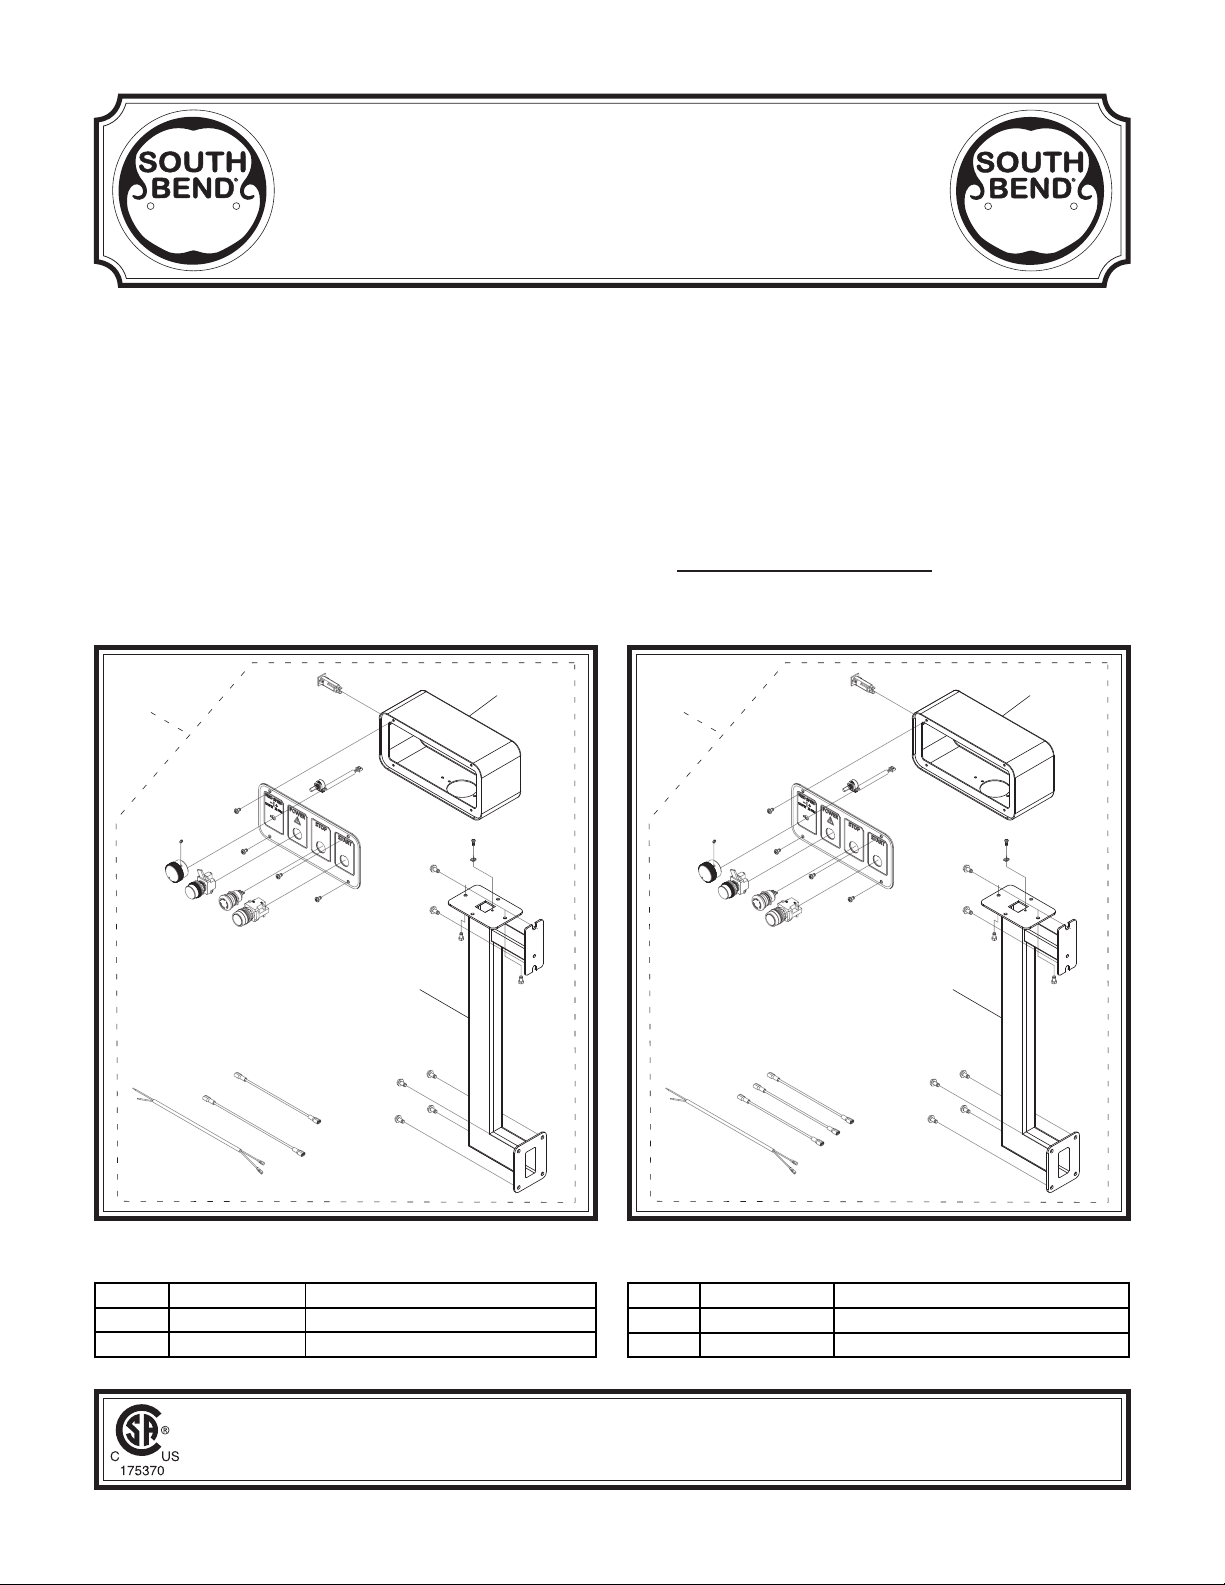
• Control panel and pedestal have been modified.
Aside from this information, all other content in the owner’s manual applies and MUST be read and
understood for your own safety. IMPORTANT: Keep this update with the owner’s manual for
future reference.
If you have any further questions about this manual update or the changes made to the machine,
contact our Technical Support at (360) 734-1540 or email www.southbendtools.com.
SB1108 Revised Parts SB1109 Revised Parts
SINCE
1906
159V2
159-4V2
159-1V2
176V2
176-1V2
176-4V2
REF PART # DESCR IPTION
159V2 PSB1108159V2 CONTROL PAN EL ASS EMB LY V2. 07.22
159-1V2 PSB1108159-1V2 CON TROL PA N EL B OX V2.07. 22
159-4 V2 PSB1108159-4V2 CONTROL PA N EL PEDES TAL V2.07.22
Copyright © June, 2022 by South Bend Tools
WARNING: No portion of this manual may be reproduced without written approval.
#MN22381 Printed in Taiwan
REF PART # DESCRIPT ION
176V2 PSB1109176V2 CONTROL PAN EL ASS EMB LY V2.07.22
176-1V2 PSB1109176-1V2 CONTROL P AN EL BOX V2.0 7.22
176-4V2 PSB1109176-4V2 SWITCH PEDESTAL V2.07.22
Page 4
15" & 20" PLANER
w/HELICAL CUTTERHEAD
MODEL SB1108/SB1109
OWNER'S MANUAL
®
South Bend Tools
A Tradition of Excellence
Copyright © December, 2020 For Machines Mfd. Since 12/20
Page 5
We stand behind our machines. If you have any service questions, parts requests or general questions
about your purchase, feel free to contact us.
South Bend Tools
P.O. Box 2027
Bellingham, WA 98227
Phone: (360) 734-1540
Fax: (360) 676-1075 (International)
Fax: (360) 734-1639 (USA Only)
Email: [email protected]
For your convenience, any updates to this manual will be available to download free of charge
www.southbendtools.com
Scope of Manual
This manual helps the reader understand the machine, how to prepare it for operation, how to control
it during operation, and how to keep it in good working condition. We assume the reader has a basic
understanding of how to operate this type of machine, but that the reader is not familiar with the
controls and adjustments of this specific model. As with all machinery of this nature, learning the
nuances of operation is a process that happens through training and experience. If you are not an
experienced operator of this type of machinery, read through this entire manual, then learn more
from an experienced operator, schooling, or research before attempting operations. Following this
advice will help you avoid serious personal injury and get the best results from your work.
We've made every effort to be accurate when documenting this machine. However, errors sometimes
happen or the machine design changes after the documentation process—so
exactly match your machine.
contact our
We highly value customer feedback on our manuals. If you have a moment, please share your
experience using this manual. What did you like about it? Is there anything you would change to
make it better? Did it meet your expectations for clarity, professionalism, and ease-of-use?
South Bend Tools
C
P.O. Box 2027
Bellingham, WA 98227
Email: [email protected]
Manual Feedback
If a difference between the manual and machine leaves you in doubt,
customer service for clarification.
the manual may not
/O Technical Documentation Manager
Updates
through our website at:
Customer Service
Page 6
Table of Contents
INTRODUCTION
Identification
Description of Controls & Components
Internal Components
Product Specifications SB1108
Product Specifications SB1109
SAFETY
Understanding Risks of Machinery
Basic Machine Safety
Additional Planer Safety
PREPARATION
Preparation Overview
Required for Setup
Power Supply Requirements
Unpacking
Inventory
Cleaning & Protecting
Location
Lifting & Moving
Assembly
Dust Collection
Checking Gearbox Oil Level
Test Run
Inspections & Adjustments
OPERATION
Operation Overview
Stock Inspection & Requirements.....................25
Wood Types
Planing Tips
Common Cutting Problems
Depth of Cut
Setting Feed Rate
Bed Roller Height
Rotating/Replacing Cutterhead Inserts
Digital Readout
ACCESSORIES
................................................................................ 9
............................................................ 15
.............................................................. 18
............................................................19
............................................................. 22
............................................................... 2
........................................................ 2
..............3
........................................... 4
............................5
............................7
.................... 9
..........................................9
................................... 11
.............................................................. 12
........................................12
............................................. 12
............................. 13
..........................................................15
.......................................17
................................................19
...................................................21
..............................22
...............................23
.................................................................... 24
........................................... 24
........................................................25
....................................................... 26
............................... 26
....................................................... 28
..............................................28
..............................................29
............30
.................................................. 31
.............................................................. 32
MAINTENANCE .............................................................34
Maintenance Schedule
Cleaning & Protecting
Machine Storage
Lubrication
Anti-Kickback Fingers
SERVICE........................................................................... 38
Tensioning/Replacing V-Belts
Setting Feed Roller, Chip Breaker & Pressure
Bar Heights
Adjusting Feed-Roller Spring Tension
Positioning Chip Deflector
Calibrating Table Height Scale
Replacing Feed Motor Brushes
Checking Pulley Alignment
Tensioning Table Height Chain
Adjusting Table Parallelism
TROUBLESHOOTING
ELECTRICAL
Electrical Safety Instructions
SB1108 Wiring Diagram
SB1108 Electrical Component Photos
SB1108 Height DRO Wiring Diagram
SB1109 Wiring Diagram
SB1109 Electrical Component Photos
SB1109 Height DRO Wiring Diagram
PARTS................................................................................57
SB1108 Main
SB1108 Table & Base
SB1108 Stand & Motor
SB1108 Labels & Cosmetics
SB1109 Main
SB1109 Table & Base
SB1109 Stand & Motor
SB1109 Labels & Cosmetics
WARRANTY
......................................................... 35
........................................................ 39
................................................................... 50
..................................................... 57
...................................................... 65
..................................................................... 73
.......................................34
.......................................34
................................................34
.......................................37
........................... 38
.............42
.................................42
.........................43
......................... 43
...............................44
........................ 44
..............................45
................................................. 47
...........................50
...................................51
..............52
..............53
...................................54
..............55
..............56
........................................60
......................................62
..............................64
........................................68
......................................70
..............................72
Page 7
South Bend Tools
Model SB1108/ SB1109
INTRODUCTION
Identification
INTRODUCTION
For Machines Mfd. Since 12/20
Serious personal injury could occur if
you connect the machine to power before
completing the setup process. DO NOT
connect power until instructed to do so later
in this manual.
-2-
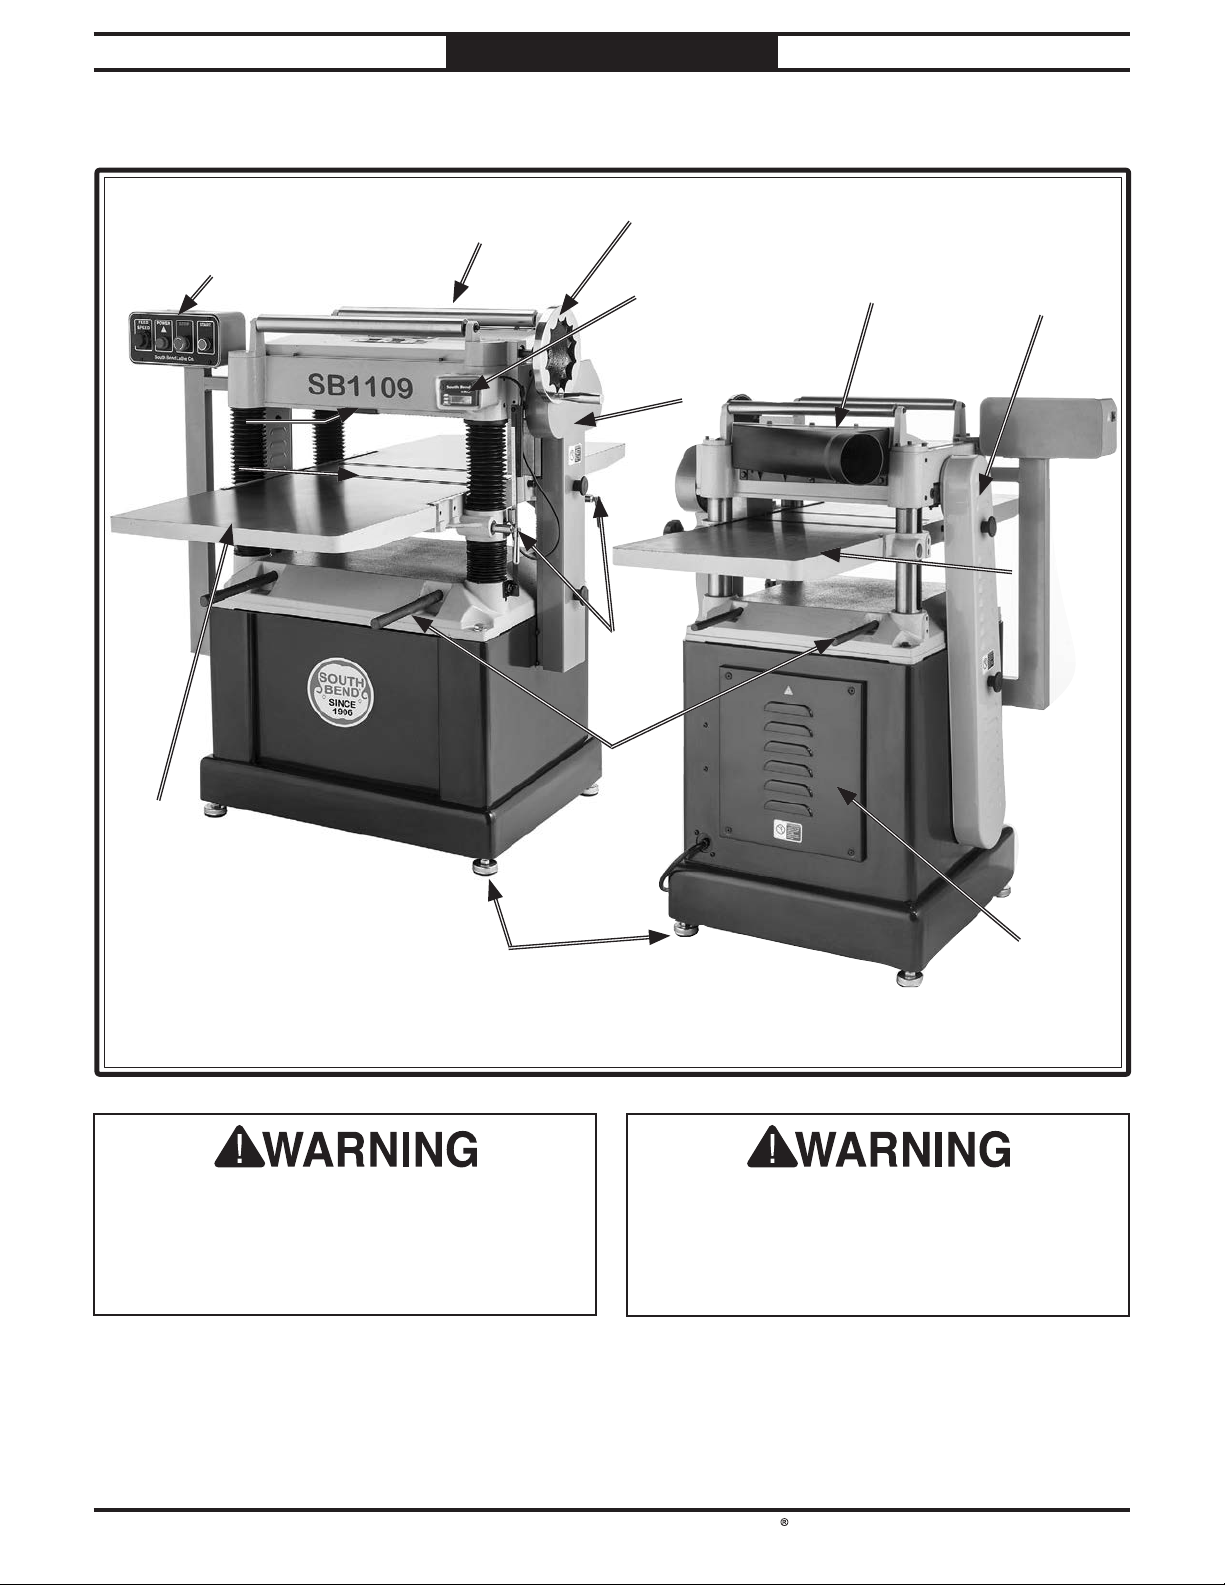
SB1108 Rear ViewSB1109 Front View
Untrained users have an increased risk
of seriously injuring themselves with this
machine. Do not operate this machine until
you have understood this entire manual and
received proper training.
Page 8
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
INTRODUCTION
Description of Controls & Components
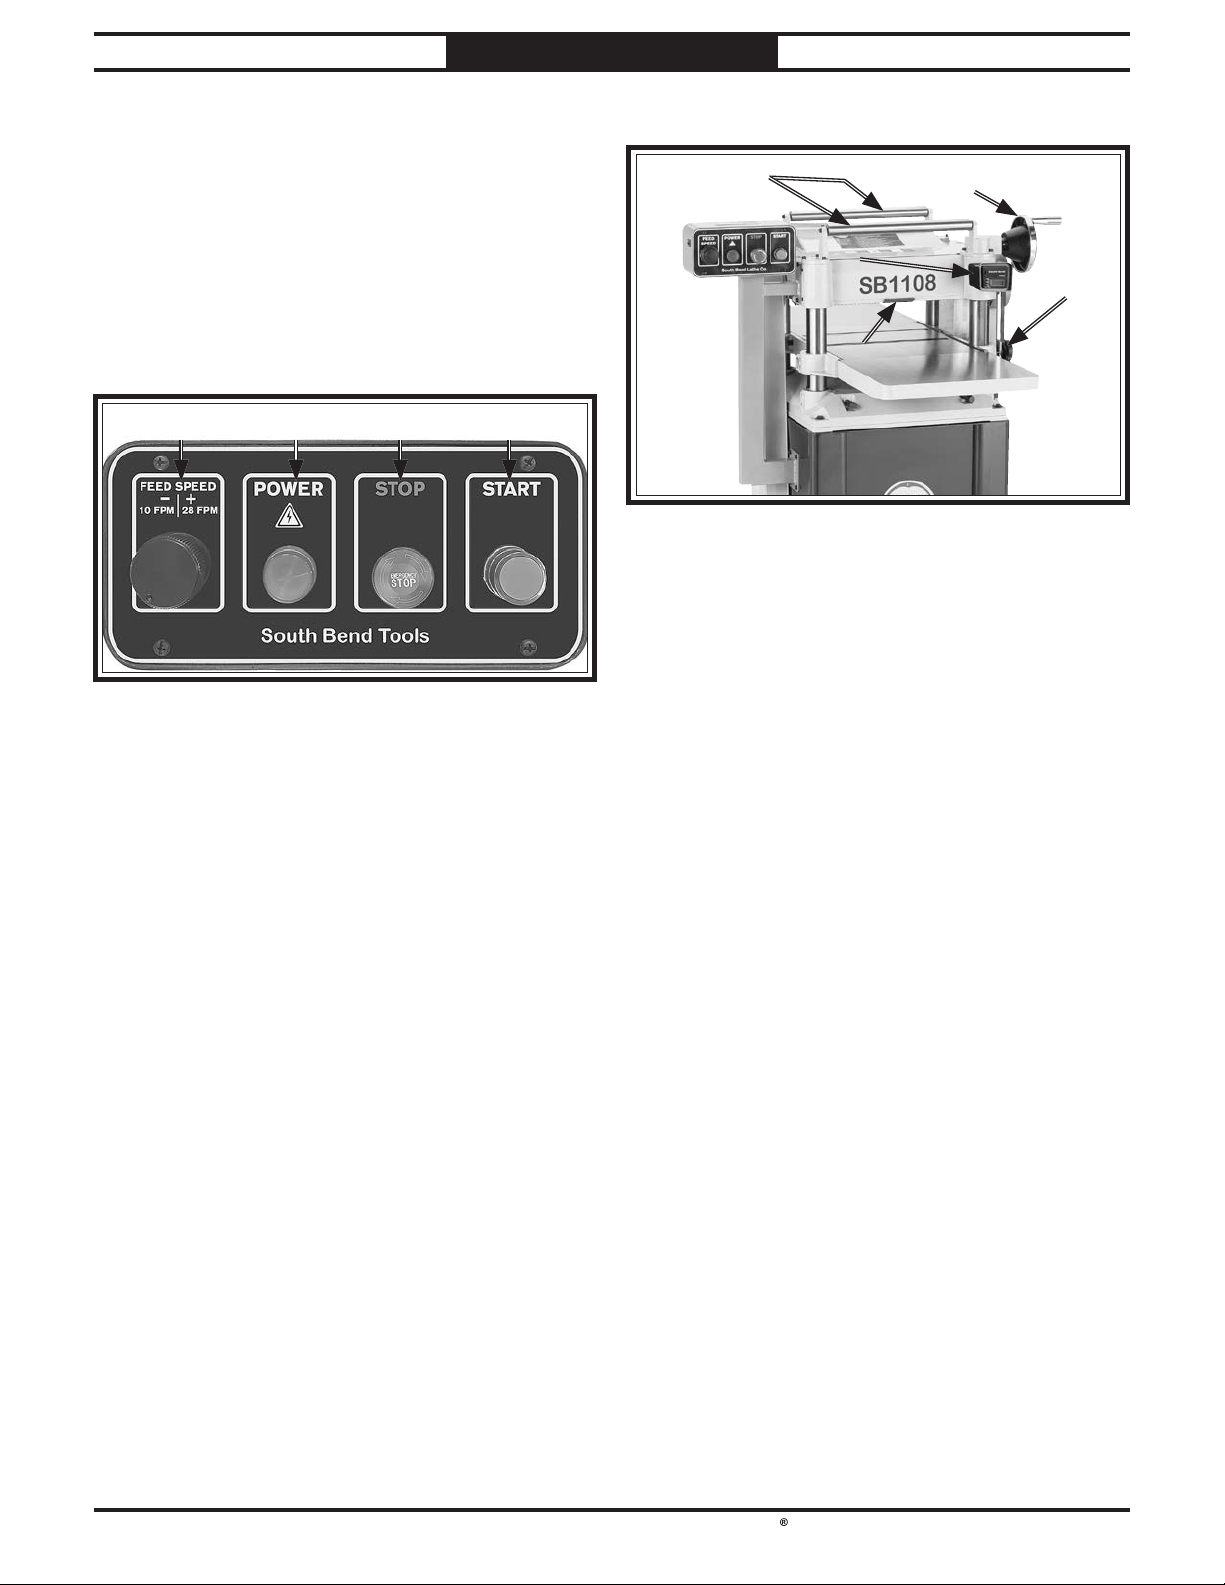
Refer to Figures 1–2 and the following
descriptions to become familiar with the basic
controls and components used to operate this
machine.
Control Panel
Figure 1. Control panel.
A. Feed Speed Control Knob: Controls the
workpiece speed (feed rate). Turn clockwise
to increase feed rate; turn counter-clockwise
to reduce feed rate.
B. Power Indicator Light: Illuminates when
power is present at control panel.
C. EMERGENCY STOP Button: Stops machine
when pressed. Rotate button clockwise until
it pops out to reset.
Operation Controls
E. Return Rollers: Assist sliding workpiece back
to feed side of planer after planing pass.
F. Table Height Handwheel: Raises and lowers
table to accommodate different workpiece
thicknesses. One complete revolution moves
the table approximately
G. Depth of Cut Digital Readout: Displays
current table height.
H. Table Locks: Secure table height position.
I. Depth Limiter: Limits maximum depth of cut.
SB1108: 3⁄32" at full width.
SB1109: 5⁄64" at full width.
1
⁄16".
D. START Button: Starts cutterhead and feed
rollers.
-3-
Page 9
South Bend Tools
Model SB1108/ SB1109
INTRODUCTION
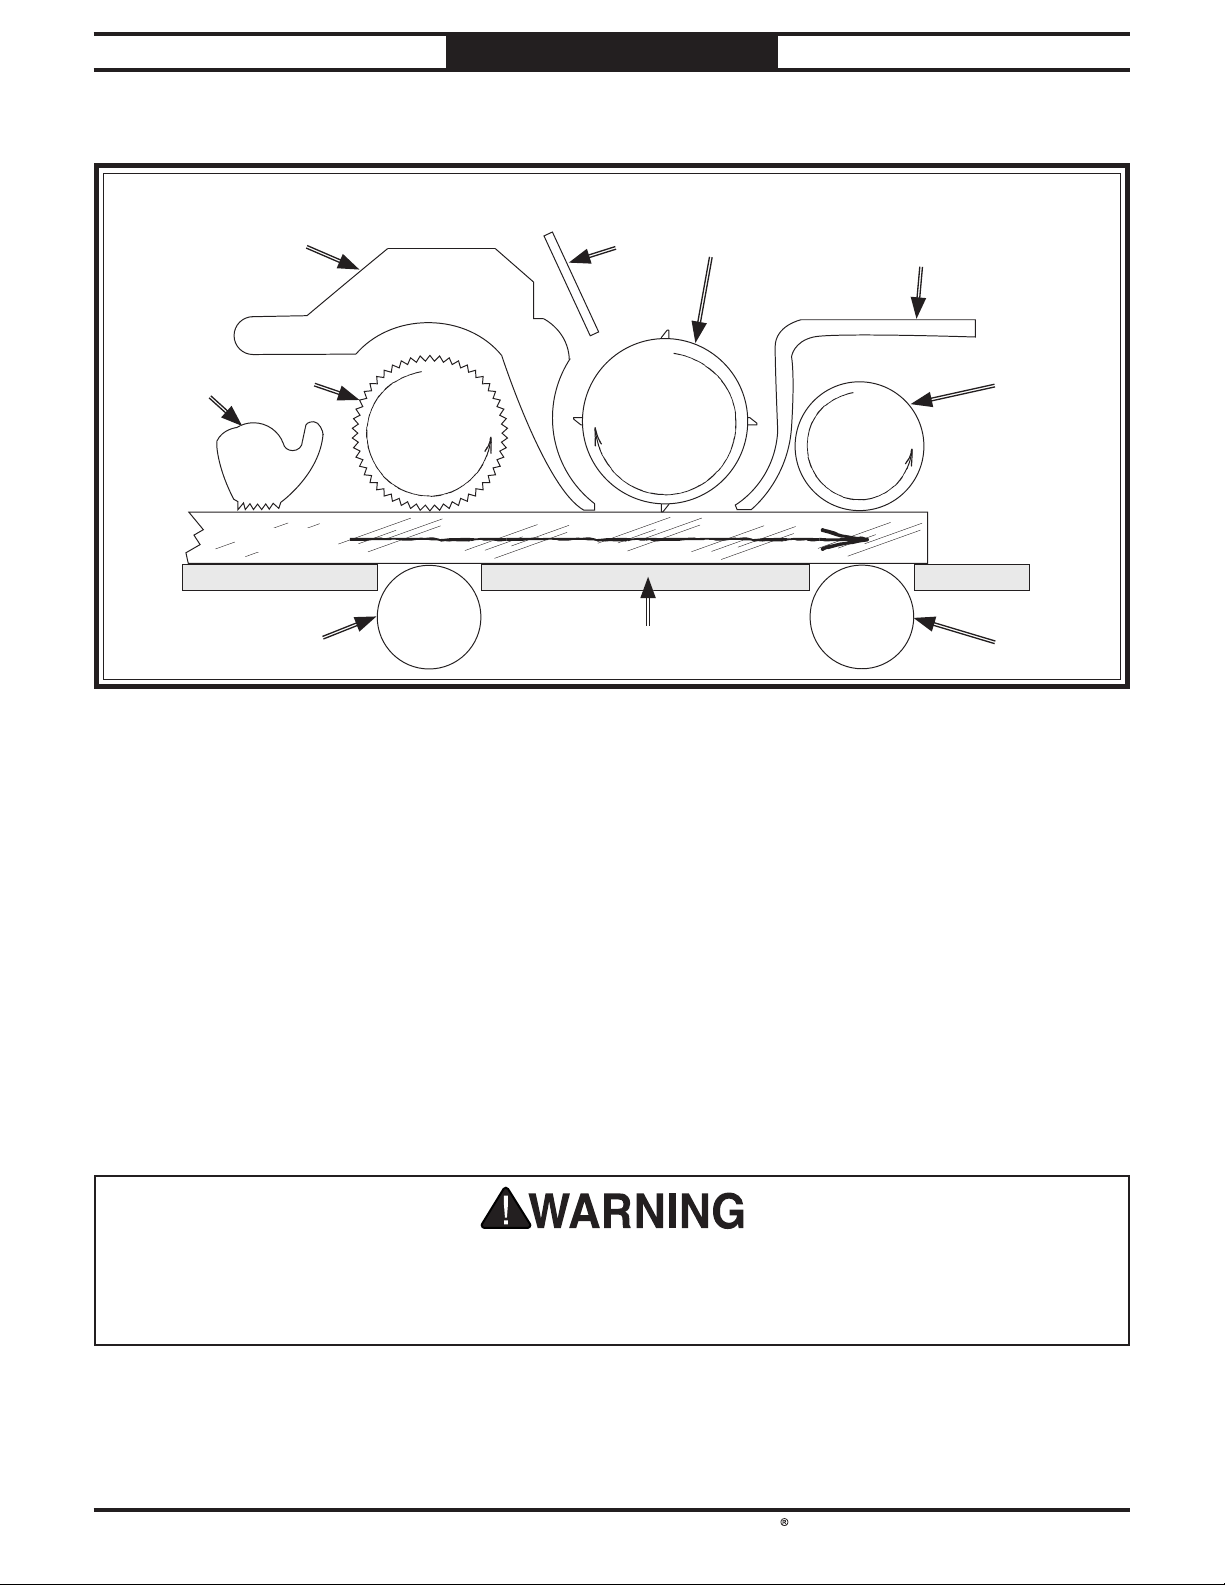
Internal Components
Front Rear
Workpiece
For Machines Mfd. Since 12/20
A. Anti-Kickback Fingers: Provide additional
safety for the operator.
B. Serrated Infeed Roller: Pulls the workpiece
toward the cutterhead.
C. Chip Breaker: Breaks off chips created by the
cutterhead to prevent tear-out and diverts
the chips to the dust hood.
D. Chip Deflector: Directs chips into the dust
hood.
E. Cutterhead: Holds the knives/indexable
carbide inserts that remove material from
the workpiece.
Like all machinery there is potential danger when operating this machine. Accidents are frequently
caused by lack of familiarity or failure to pay attention. Use this machine with respect and caution
to decrease the risk of operator injury. If normal safety precautions are overlooked or ignored,
serious personal injury may occur.
F. Pressure Bar: Stabilizes the workpiece
as it leaves the cutterhead and assists in
deflecting wood particles toward the dust
hood.
G. Outfeed Roller: Pulls the workpiece through
the planer.
H. Bed Rollers: Provide upward pressure on the
workpiece, enabling the feed rollers to pull
the workpiece along.
I. Planer Table: Provides a smooth and level
path for the workpiece as it moves through
the planer.
-4-
Page 10
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
INTRODUCTION
Product Specifications SB1108
Model SB1108
15" Planer with Helical Cutterhead
Product Dimensions
Weight.............................................................................................................................................................
Width (side-to-side) x Depth (front-to-back) x Height............................................................... 39 x 48 x 44-1/2 in.
Footprint (Length x Width)................................................................................................................. 23 x 22-1/2 in.
Shipping Dimensions
Type.......................................................................................................................................................... Wood Crate
Content..........................................................................................................................................................
Weight.............................................................................................................................................................
Length x Width x Height................................................................................................................... 27 x 37 x 52 in.
Must Ship Upright................................................................................................................................................ Yes
509 lbs.
Machine
595 lbs.
Electrical
Power Requirement......................................................................................................... 230V, Single-Phase, 60 Hz
Full-Load Current Rating....................................................................................................................................
Minimum Circuit Size..........................................................................................................................................
Connection Type..................................................................................................................................... Cord & Plug
Power Cord Included............................................................................................................................................. Yes
Power Cord Length.......................................................................................................................................... 120 in.
Power Cord Gauge.........................................................................................................................................
Plug Included........................................................................................................................................................
Included Plug Type.............................................................................................................................................. 6-20
Switch Type................................................................................ Magnetic Switch w/Thermal Overload Protection
Motors
Main
Horsepower............................................................................................................................................... 3 HP
Phase............................................................................................................................................
Amps...........................................................................................................................................................
Speed................................................................................................................................................ 3450 RPM
Type............................................................................................................. TEFC Capacitor-Start Induction
Power Transfer ........................................................................................................................... Triple V-Belt
Bearings....................................................................................................
Centrifugal Switch/Contacts Type.....................................................................................................
Feed
Horsepower............................................................................................................................................ 3/4 HP
Amps............................................................................................................................................................. 8A
Speed................................................................................................................................................ 2500 RPM
Type...................................................................................................................................................
Power Transfer ...........................................................................................................................
Bearings................................................................................................... Sealed & Permanently Lubricated
Sealed & Permanently Lubricated
18A
20A
12 AWG
Yes
Single-Phase
12A
External
DC Motor
Belt & Chain
-5-
Page 11
South Bend Tools
Model SB1108/ SB1109
Main Specifications
Main Specifications
Planer Size...............................................................................................................................................
Max. Cut Width.......................................................................................................................................
Max. Cut Height........................................................................................................................................ 6 in.
Min. Stock Length..................................................................................................................................... 6 in.
Min. Stock Thickness............................................................................................................................ 3/16 in.
Number of Cuts Per Inch.....................................................................................................................
Number of Cuts Per Minute..................................................................................................................
Cutterhead Speed............................................................................................................................ 5000 RPM
Planing Feed Rate........................................................................................................................ 10 - 28 FPM
Max. Cut Depth Planing Full Width................................................................................................... 3/32 in.
Max. Cut Depth Planing 6-Inch Wide Board........................................................................................
Cutterhead Info
Cutterhead Type....................................................................................................................................
Cutterhead Diameter ................................................................................................................................ 3 in.
Number of Cutter Rows.................................................................................................................................. 4
Number of Indexable Cutters....................................................................................................................... 52
Cutter Insert Type..............................................................................................................
Cutter Insert Size Length......................................................................................................................
Cutter Insert Size Width........................................................................................................................ 15mm
Cutter Insert Size Thickness................................................................................................................ 2.5mm
INTRODUCTION
For Machines Mfd. Since 12/20
15 in.
15 in.
167 - 60
20,000
1/8 in.
Helical
Indexable Carbide
15mm
Table Info
Table/Headstock Movement...................................................................................................................... 6 in.
Table Bed Size Length.............................................................................................................................
Table Bed Size Width..............................................................................................................................
Table Bed Size Thickness.......................................................................................................................... 2 in.
Number of Bed Rollers.................................................................................................................................... 2
Floor-to-Table Height....................................................................................................................... 30 - 36 in.
Table Wings Size Length.........................................................................................................................
Table Wings Size Width..................................................................................................................
Construction
Table.................................................................................................................... Precision-Ground Cast Iron
Body................................................................................................................................................... Cast Iron
Stand......................................................................................................................................................... Steel
Cutterhead Assembly...............................................................................................................................
Infeed Roller..............................................................................................................................
Outfeed Roller............................................................................................................................. Smooth Steel
Paint Type/Finish.................................................................................................................... Powder Coated
Other
Table/Headstock Locks............................................................................................................................... Yes
Measurement Scale...................................................................................................................
Number of Dust Ports.....................................................................................................................................
Dust Port Size............................................................................................................................................ 4 in.
Mobile Base........................................................................................................................................... T28000
Serrated Steel
48 in.
15 in.
14 in.
15-1/16 in.
Steel
Inch & Metric
1
Other
Country of Origin ........................................................................................................................................... Taiwan
Warranty ......................................................................................................................................................... 1 Year
Approximate Assembly & Setup Time .......................................................................................................... 1 Hour
Serial Number Location .............................................................................................................................. ID Label
Certified by a Nationally Recognized Testing Laboratory (NRTL) ................................................................... Yes
-6-
Page 12
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
INTRODUCTION
Product Specifications SB1109
Model SB1109
20" Planer with Helical Cutterhead
Product Dimensions
Weight.............................................................................................................................................................
Width (side-to-side) x Depth (front-to-back) x Height............................................................... 46-1/2 x 56 x 46 in.
Footprint (Length x Width)........................................................................................................... 23-1/2 x 29-1/2 in.
Shipping Dimensions
Type.......................................................................................................................................................... Wood Crate
Content..........................................................................................................................................................
Weight.............................................................................................................................................................
Length x Width x Height................................................................................................................... 42 x 30 x 52 in.
Must Ship Upright................................................................................................................................................ Yes
719 lbs.
Machine
820 lbs.
Electrical
Power Requirement......................................................................................................... 220V, Single-Phase, 60 Hz
Full-Load Current Rating....................................................................................................................................
Minimum Circuit Size..........................................................................................................................................
Connection Type..................................................................................................................................... Cord & Plug
Power Cord Included............................................................................................................................................. Yes
Power Cord Length.......................................................................................................................................... 120 in.
Power Cord Gauge.........................................................................................................................................
Plug Included........................................................................................................................................................
Included Plug Type............................................................................................................................................ L6-30
Switch Type................................................................................ Magnetic Switch w/Thermal Overload Protection
Motors
Main
Horsepower.............................................................................................................................................. 5 HP
Phase............................................................................................................................................
Amps...........................................................................................................................................................
Speed................................................................................................................................................ 3450 RPM
Type............................................................................................................. TEFC Capacitor-Start Induction
Power Transfer ........................................................................................................................... Triple V-Belt
Bearings....................................................................................................
Centrifugal Switch/Contacts Type.....................................................................................................
Feed
Horsepower............................................................................................................................................ 3/4 HP
Amps............................................................................................................................................................. 8A
Speed................................................................................................................................................ 2500 RPM
Type...................................................................................................................................................
Power Transfer ...........................................................................................................................
Bearings.................................................................................................... Sealed & Permanently Lubricated
Sealed & Permanently Lubricated
27A
30A
12 AWG
Yes
Single-Phase
23A
External
DC Motor
Belt & Chain
-7-
Page 13
South Bend Tools
Model SB1108/ SB1109
Main Specifications
Main Specifications
Planer Size...............................................................................................................................................
Max. Cut Width.......................................................................................................................................
Max. Cut Height........................................................................................................................................ 8 in.
Min. Stock Length..................................................................................................................................... 7 in.
Min. Stock Thickness.............................................................................................................................. 1/4 in.
Number of Cuts Per Inch.....................................................................................................................
Number of Cuts Per Minute..................................................................................................................
Cutterhead Speed............................................................................................................................ 5000 RPM
Planing Feed Rate........................................................................................................................ 10 - 28 FPM
Max. Cut Depth Planing Full Width................................................................................................... 5/64 in.
Max. Cut Depth Planing 6-Inch Wide Board........................................................................................
Cutterhead Info
Cutterhead Type....................................................................................................................................
Cutterhead Diameter ......................................................................................................................... 3-1/4 in.
Number of Cutter Rows.................................................................................................................................. 4
Number of Indexable Cutters....................................................................................................................... 92
Cutter Insert Type..............................................................................................................
Cutter Insert Size Length......................................................................................................................
Cutter Insert Size Width........................................................................................................................ 15mm
Cutter Insert Size Thickness................................................................................................................ 2.5mm
INTRODUCTION
For Machines Mfd. Since 12/20
20 in.
20 in.
167 - 60
20,000
1/8 in.
Helical
Indexable Carbide
15mm
Table Info
Table/Headstock Movement...................................................................................................................... 8 in.
Table Bed Size Length.............................................................................................................................
Table Bed Size Width..............................................................................................................................
Table Bed Size Thickness.................................................................................................................... 2-1/4 in.
Number of Bed Rollers.................................................................................................................................... 2
Floor-to-Table Height....................................................................................................................... 28 - 36 in.
Table Wings Size Length.........................................................................................................................
Table Wings Size Width....................................................................................................................
Construction
Table.................................................................................................................... Precision-Ground Cast Iron
Body................................................................................................................................................... Cast Iron
Stand......................................................................................................................................................... Steel
Cutterhead Assembly...............................................................................................................................
Infeed Roller..............................................................................................................................
Outfeed Roller............................................................................................................................. Smooth Steel
Paint Type/Finish.................................................................................................................... Powder Coated
Other
Table/Headstock Locks............................................................................................................................... Yes
Measurement Scale...................................................................................................................
Number of Dust Ports.....................................................................................................................................
Dust Port Size............................................................................................................................................ 5 in.
Mobile Base........................................................................................................................................... T28000
Serrated Steel
56 in.
20 in.
15 in.
21-1/4 in.
Steel
Inch & Metric
1
Other
Country of Origin ........................................................................................................................................... Taiwan
Warranty ........................................................................................................................................................ 2 Years
Approximate Assembly & Setup Time .......................................................................................................... 1 Hour
Serial Number Location .............................................................................................................................. ID Label
Certified by a Nationally Recognized Testing Laboratory (NRTL) ................................................................... Yes
-8-
Page 14
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
Operating all machinery and machining equipment can be dangerous or relatively safe depending
on how it is installed and maintained, and the operator's experience, common sense, risk awareness,
working conditions, and use of personal protective equipment (safety glasses, respirators, etc.).
The owner of this machinery or equipment is ultimately responsible for its safe use. This
responsibility includes proper installation in a safe environment, personnel training and usage
authorization, regular inspection and maintenance, manual availability and comprehension,
application of safety devices, integrity of cutting tools or accessories, and the usage of approved
personal protective equipment by all operators and bystanders.
The manufacturer of this machinery or equipment will not be held liable for injury or property
damage from negligence, improper training, machine modifications, or misuse. Failure to read,
understand, and follow the manual and safety labels may result in serious personal injury, including
amputation, broken bones, electrocution, or death.
The signals used in this manual to identify hazard levels are as follows:
Owner’s Manual: All machinery and machining
Trained/Supervised Operators Only: Untrained
SAFETY
SAFETY
Understanding Risks of Machinery
Death or catastrophic
harm WILL occur.
Death or catastrophic
harm COULD occur.
Moderate injury or fire
MAY occur.
Machine or property
damage may occur.
Basic Machine Safety
equipment presents serious injury hazards
to untrained users. To reduce the risk of
injury, anyone who uses THIS item MUST
read and understand this entire manual
before starting.
Personal Protective Equipment:
servicing this item may expose the user
to flying debris, dust, smoke, dangerous
chemicals, or loud noises. These hazards
can result in eye injury, blindness, longterm respiratory damage, poisoning,
cancer, reproductive harm or hearing loss.
Reduce your risks from these hazards
by wearing approved eye protection,
respirator, gloves, or hearing protection.
Operating or
users can seriously injure themselves
or bystanders. Only allow trained and
properly supervised personnel to operate
this item. Make sure safe operation
instructions are clearly understood. If
electrically powered, use padlocks and
master switches, and remove start switch
keys to prevent unauthorized use or
accidental starting.
Guards/Covers:
moving parts during operation may cause
severe entanglement, impact, cutting,
or crushing injuries. Reduce this risk by
keeping any included guards/covers/doors
installed, fully functional, and positioned
for maximum protection.
Accidental contact with
-9-
Page 15
South Bend Tools
Model SB1108/ SB1109
Entanglement: Loose clothing, gloves, neckties,
rotate.
Chuck Keys or Adjusting Tools:
Tools used to
our Technical Support for assistance.
SAFETY
For Machines Mfd. Since 12/20
jewelry or long hair may get caught in
moving parts, causing entanglement,
amputation, crushing, or strangulation.
Reduce this risk by removing/securing
these items so they cannot contact moving
parts.
Mental Alertness: Operating this item with
reduced mental alertness increases the
risk of accidental injury. Do not let a
temporary influence or distraction lead to a
permanent disability! Never operate when
under the influence of drugs/alcohol, when
tired, or otherwise distracted.
Safe Environment:
powered equipment in a wet environment
may result in electrocution; operating near
highly flammable materials may result in a
fire or explosion. Only operate this item in
a dry location that is free from flammable
materials.
Electrical Connection: With electically powered
equipment, improper connections to the
power source may result in electrocution
or fire. Always adhere to all electrical
requirements and applicable codes when
connecting to the power source. Have all
work inspected by a qualified electrician to
minimize risk.
Disconnect Power: Adjusting or servicing
electrically powered equipment while it
is connected to the power source greatly
increases the risk of injury from accidental
startup. Always disconnect power
BEFORE any service or adjustments,
including changing blades or other tooling.
Operating electrically
adjust spindles, chucks, or any moving/
rotating parts will become dangerous
projectiles if left in place when the machine
is started. Reduce this risk by developing
the habit of always removing these tools
immediately after using them.
Work Area:
the risks of accidental injury. Only operate
this item in a clean, non-glaring, and welllighted work area.
Properly Functioning Equipment:
maintained, damaged, or malfunctioning
equipment has higher risks of causing
serious personal injury compared to
those that are properly maintained.
To reduce this risk, always maintain
this item to the highest standards and
promptly repair/service a damaged or
malfunctioning component. Always follow
the maintenance instructions included in
this documentation.
Unattended Operation:
equipment that is left unattended while
running cannot be controlled and is
dangerous to bystanders. Always turn the
power OFF before walking away.
Health Hazards: Certain cutting fluids and
lubricants, or dust/smoke created when
cutting, may contain chemicals known to
the State of California to cause cancer,
respiratory problems, birth defects,
or other reproductive harm. Minimize
exposure to these chemicals by wearing
approved personal protective equipment
and operating in a well ventilated area.
Clutter and dark shadows increase
Poorly
Electrically powered
Secure Workpiece/Tooling:
cutting tools, or rotating spindles can
become dangerous projectiles if not
secured or if they hit another object during
operation. Reduce the risk of this hazard
by verifying that all fastening devices are
properly secured and items attached to
spindles have enough clearance to safely
-10-
Loose workpieces,
Difficult Operations:
operations with which you are unfamiliar
increases the risk of injury. If you
experience difficulties performing the
intended operation, STOP! Seek an
alternative method to accomplish the
same task, ask a qualified expert how the
operation should be performed, or contact
Attempting difficult
Page 16
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
Amputation, serious cuts, entanglement, or death can occur from contact with rotating cutterhead or
other moving parts! Flying chips can cause eye injuries or blindness. Workpieces or knives thrown
by cutterhead can strike nearby operator or bystanders with deadly force. To reduce the risk of these
hazards, operator and bystanders MUST completely heed hazards and warnings below.
Kickback:
Avoid Contact with Moving Parts:
Dull/Damaged Knives/Inserts:
Inspecting Stock:
Body Placement:
Grain Direction:
with the wood grain.
SAFETY
Additional Planer Safety
Know how to reduce the risk of
kickback and kickback-related injuries.
“Kickback” occurs during the operation
when the workpiece is ejected back from the
infeed side of the machine at a high rate
of speed. Kickback is commonly caused by
poor workpiece selection, unsafe feeding
techniques, or improper machine setup/
maintenance. Kickback injuries typically
occur as follows: (1) operator/bystanders
are struck by the workpiece, resulting in
impact injuries (i.e., blindness, broken bones,
bruises, death); (2) operator’s hands are
pulled into the machine from the outfeed
side, resulting in amputation or severe
lacerations.
Never remove
guards/covers or reach inside the planer
during operation or while connected to
power. You could be seriously injured if you
accidentally touch the spinning cutterhead
or get entangled in moving parts. If a
workpiece becomes stuck or sawdust removal
is necessary, turn planer OFF, allow
cutterhead to stop, and disconnect power
before clearing.
Only use sharp,
undamaged knives/inserts. Dull or damaged
knives/inserts increase the risk of kickback.
To reduce the risk of kickback
injuries or machine damage, thoroughly
inspect and prepare the workpiece before
cutting. Verify workpiece is free of nails,
staples, loose knots, or foreign material.
Workpieces with minor warping should be
jointed first or planed with the cupped side
facing the table.
Stand to one side of planer
during the entire operation to avoid getting
hit if kickback occurs.
Planing across the grain is hard
on the planer and may cause kickback. Plane
in the same direction or at a slight angle
Planing Correct Material: Only plane natural
wood stock with this planer. DO NOT
plane MDF, OSB, plywood, laminates
or other synthetic materials that can
break up inside the planer and be ejected
towards the operator.
Looking Inside Planer: Wood chips fly around
inside the planer at a high rate of speed
during operation. To avoid injury from
flying material, DO NOT look inside
planer during operation.
Cutting Limitations: To reduce the risk of
kickback hazards or damage to the
machine, do not exceed the maximum
depth of cut or minimum board length and
thickness found in the Data Sheet. Only
feed one board at a time.
Infeed Roller Clearance: The infeed roller
is designed to pull material into the
spinning cutterhead. To reduce the risk
of entanglement, keep hands, clothing,
jewelry, and long hair away from the
infeed roller during operation.
Feed Workpiece Properly: To reduce the risk
of kickback, never start planer with
workpiece touching cutterhead. Allow
cutterhead to reach full speed before
feeding, and do not change feed speed
during cutting operation.
Workpiece Support: To reduce the risk of
kickback, always make sure workpiece
can move completely across table without
rocking or tipping. Use auxiliary support
stands for long stock.
Secure Knives/Inserts: Loose knives or
improperly set inserts can become
dangerous projectiles or cause machine
damage. Always verify knives/inserts
are secure and properly adjusted before
operation.
-11-
Page 17
South Bend Tools
Model SB1108/ SB1109
PREPARATION
PREPARATION
For Machines Mfd. Since 12/20
Preparation Overview Required for Setup
The purpose of the preparation section is to help
you prepare your machine for operation. The list
below outlines the basic process. Specific steps
for each of these points will be covered in detail
later in this section.
The typical preparation process is as follows:
1. Unpack the machine and inventory the
contents of the box/crate.
Clean the machine and its components.
2.
3. Identify an acceptable location for the
machine and move it to that location.
Level the machine using the pre-installed
4.
machine mounts.
Assemble the loose components and make
5.
any necessary adjustments or inspections to
ensure the machine is ready for operation.
Connect the machine to the power source.
6.
7. Test run the machine to make sure it
functions properly and is ready for operation.
The items listed below are required to
successfully set up and prepare this machine for
operation.
For Lifting
• A forklift or other power lifting device rated
for the weight of the machine.
• Lifting Strap or Chain (rated for at least 1000
lbs.)
For Power Connection
• A power source that meets the minimum circuit requirements for this machine. (Refer to
the Power Supply Requirements on Page
13 for details.)
For Assembly
• Safety Glasses (for each person)
• Straightedge 4' (or longer)
• Dust Collection System
• 4" Dust Hose (for SB1108)
• 4" Hose Clamp (for SB1108)
• 5" Dust Hose (for SB1109)
• 5" Hose Clamp (for SB1109)
• Disposable Rags
• Disposable Gloves
• Cleaner/Degreaser
• Gearbox Oil
• Phillips Head Screwdriver #2
• Open-End Wrench 8mm (for SB1108)
• Open-End Wrench 17mm (for SB1109)
-12-
Page 18
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
Before installing the machine, consider the
availability and proximity of the required power
supply circuit. If an existing circuit does not meet
the requirements for this machine, a new circuit
must be installed.
To minimize the risk of electrocution, fire,
or equipment damage, installation work and
electrical wiring must be done by a
or qualified service personnel
applicable electrical codes and safety standards.
The full-load current rating is the amperage
a machine draws at 100% of the rated output
power. On machines with multiple motors, this is
the amperage drawn by the largest motor or sum
of all motors and electrical devices that might
operate at one time during normal operations.
The full-load current is not the maximum
amount of amps that the machine will draw. If
the machine is overloaded, it will draw additional
amps beyond the full-load rating.
If the machine is overloaded for a sufficient
length of time, damage, overheating, or fire may
result—especially if connected to an undersized
circuit. To reduce the risk of these hazards,
avoid overloading the machine during operation
and make sure it is connected to a power supply
circuit that meets the requirements in the
following section.
Note: The circuit requirements in this manual
are for
machine will be running at a time. If this
machine will be connected to a shared circuit
where multiple machines will be running at
the same time, consult a qualified electrician to
ensure the circuit is properly sized.
A power supply circuit includes all electrical
equipment between the main breaker box or fuse
panel in your building and the incoming power
connections inside the machine. This circuit
must be safely sized to handle the full-load
current that may be drawn from the machine for
an extended period of time. (If this machine is
connected to a circuit protected by fuses, use a
time delay fuse marked D.)
This machine must be grounded! In the event
of
grounding provides a path of least resistance
for electric current
electric shock.
Improper connection of the equipment-grounding
wire can result in a risk of electric shock. The
wire with green insulation (with or without
yellow stripes) is the equipment-grounding wire.
If repair or replacement of the power cord or
plug is necessary, do not connect the equipmentgrounding wire to a live (current carrying)
terminal.
Check with an electrician or qualified service
personnel if you do not understand these
grounding requirements, or if you are in doubt
about whether the tool is properly grounded.
If you ever notice that a cord or plug is
damaged or worn, disconnect it from power, and
immediately replace it with a new one.
PREPARATION
Power Supply Requirements
Availability
in accordance with
Electrocution or fire may
occur if machine is not
correctly grounded and
attached to the power
supply. Use a qualified
electrician to ensure a safe
power connection.
Circuit Information
Power supply requirements
a dedicated circuit—where only one
n electrician
For your own safety and protection of property,
consult an electrician if you are unsure about
wiring practices or applicable electrical codes.
Grounding Requirements
Full-Load Current Rating at 220V
SB1108 Full-Load Rating ................... 18 Amps
SB1109 Full-Load Rating
................... 27 Amps
certain types of malfunctions or breakdowns,
in order to reduce the risk of
-13 -
Page 19
South Bend Tools
Model SB1108/ SB1109
This machine is prewired to operate on a power
supply circuit that has a verified ground and
meets the following requirements:
This machine is prewired to operate on a power
supply circuit that has a verified ground and
meets the following requirements:
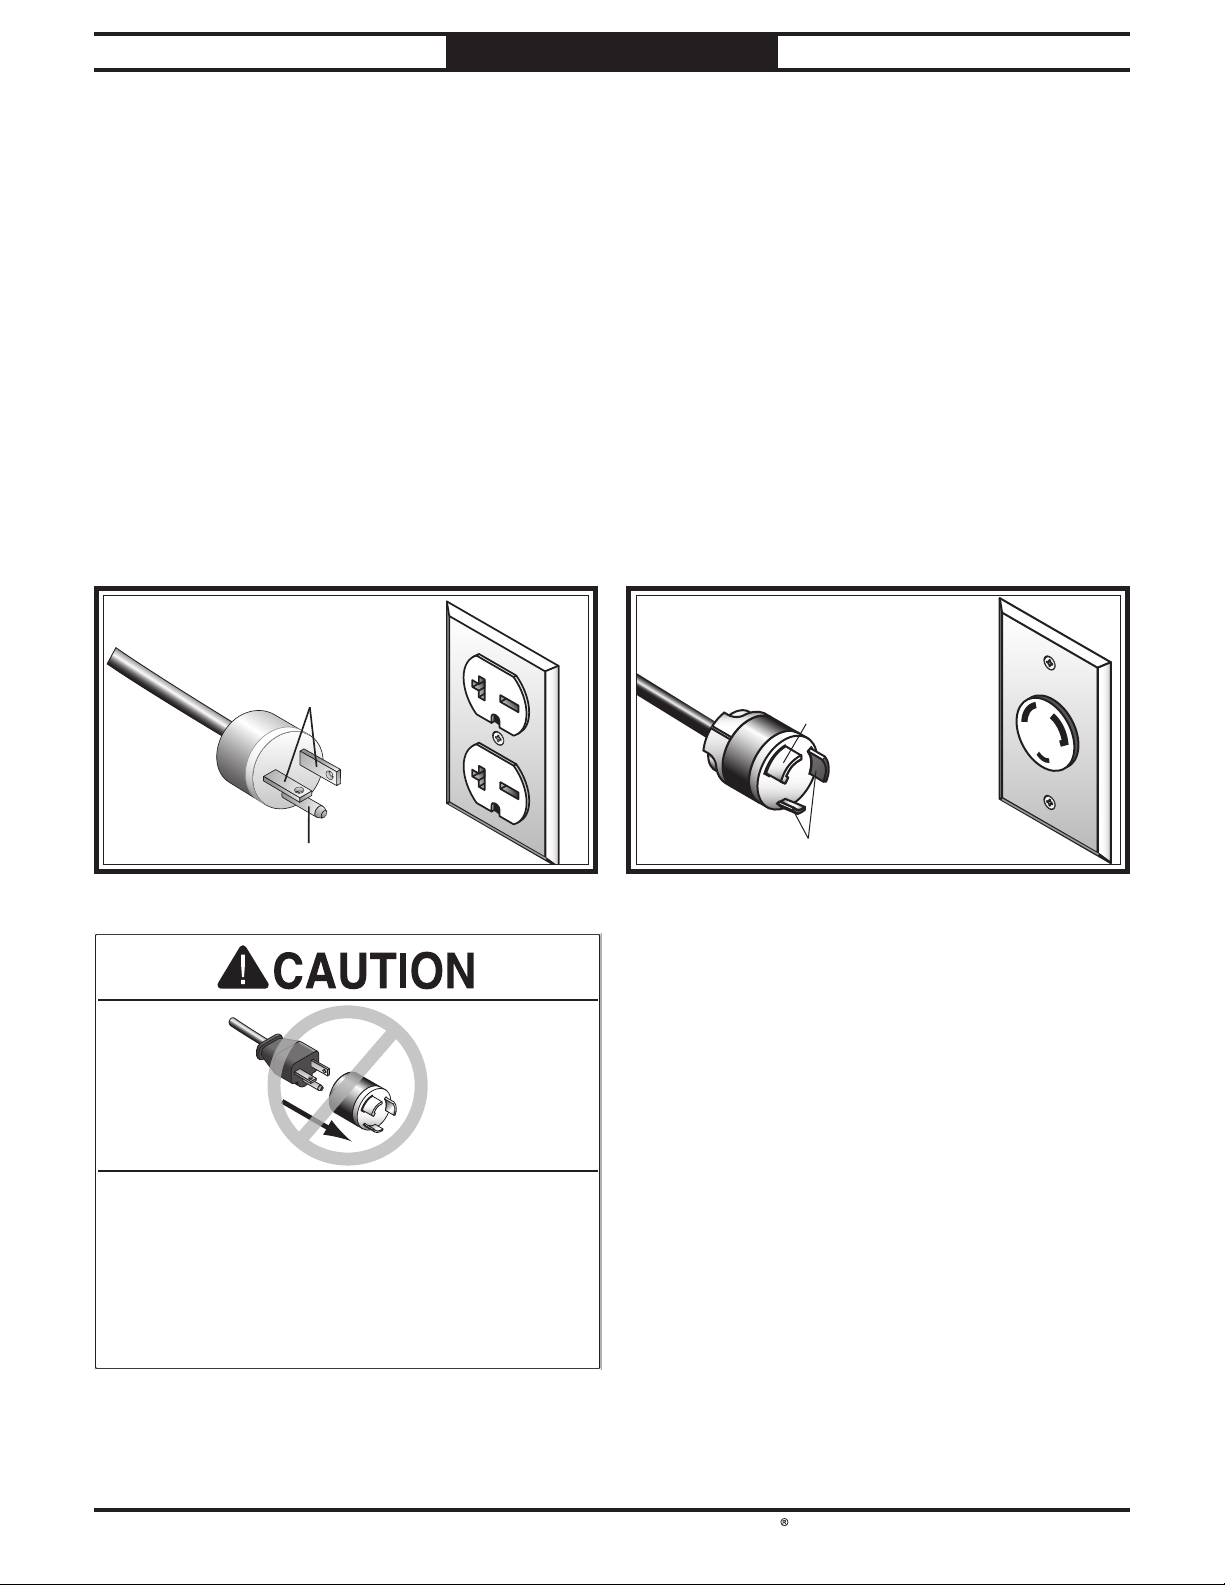
This machine is equipped with a power cord
that has
grounding plug
The plug
receptacle (outlet)
grounded in accordance with all local codes and
ordinances.
This machine is equipped with a power cord
that has
grounding plug
The plug
receptacle (outlet)
grounded in accordance with all local codes and
ordinances.
We do not recommend using an extension cord
with this machine. If you must use one, only
use it if absolutely necessary and only on a
temporary basis.
Extension cords cause voltage drop, which may
damage electrical components and shorten motor
life. Voltage drop increases as the extension cord
size gets longer and the gauge size gets smaller
(higher gauge numbers indicate smaller sizes).
Any extension cord used with this machine
must contain a ground wire, match the required
plug and receptacle listed in the
Requirements
meet the following requirements:
PREPARATION
For Machines Mfd. Since 12/20
SB1108 Circuit Requirements
Nominal Voltage ........ 208V, 220V, 230V, 240V
Cycle
Phase
Circuit Rating....................................... 20 Amps
Plug/Receptacle (included)
.............................................................60 Hz
..............................................Single-Phase
...........NEMA 6-20
an equipment-grounding wire and a
(similar to the figure below).
must only be inserted into a matching
that is properly installed and
GROUNDED
6-20 RECEPTACLE
Current Carrying Prongs
SB1109 Circuit Requirements
Nominal Voltage ........ 208V, 220V, 230V, 240V
Cycle
Phase
Circuit Rating....................................... 30 Amps
Plug/Receptacle (included)
.............................................................60 Hz
..............................................Single-Phase
........ NEMA L6-30
an equipment-grounding wire and a
(similar to the figure below).
must only be inserted into a matching
that is properly installed and
GROUNDED
L6-30 LOCKING
RECEPTACLE
Grounding Prong
is Hooked
6-20 PLUG
Grounding Prong
No adapter should be used with plug. If
plug does not fit available receptacle, or if
machine must be reconnected for use on a
different type of circuit, reconnection must
be performed by an electrician or qualified
service personnel, and it must comply with all
local codes and ordinances.
-14-
L6-30
LOCKING
PLUG
Current Carrying Prongs
Extension Cords
Circuit
for the applicable voltage, and
SB1108 .............................. 12 AWG, 50 ft or less
SB1109
.............................. 10 AWG, 50 ft or less
Page 20
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
This item was carefully packaged to prevent
damage during transport. If you discover any
damage, please immediately call Customer
Service at (360) 734-1540 for advice. You may
need to file a freight claim, so take pictures and
save all the containers and packing materials for
possible inspection by the carrier or its agent.
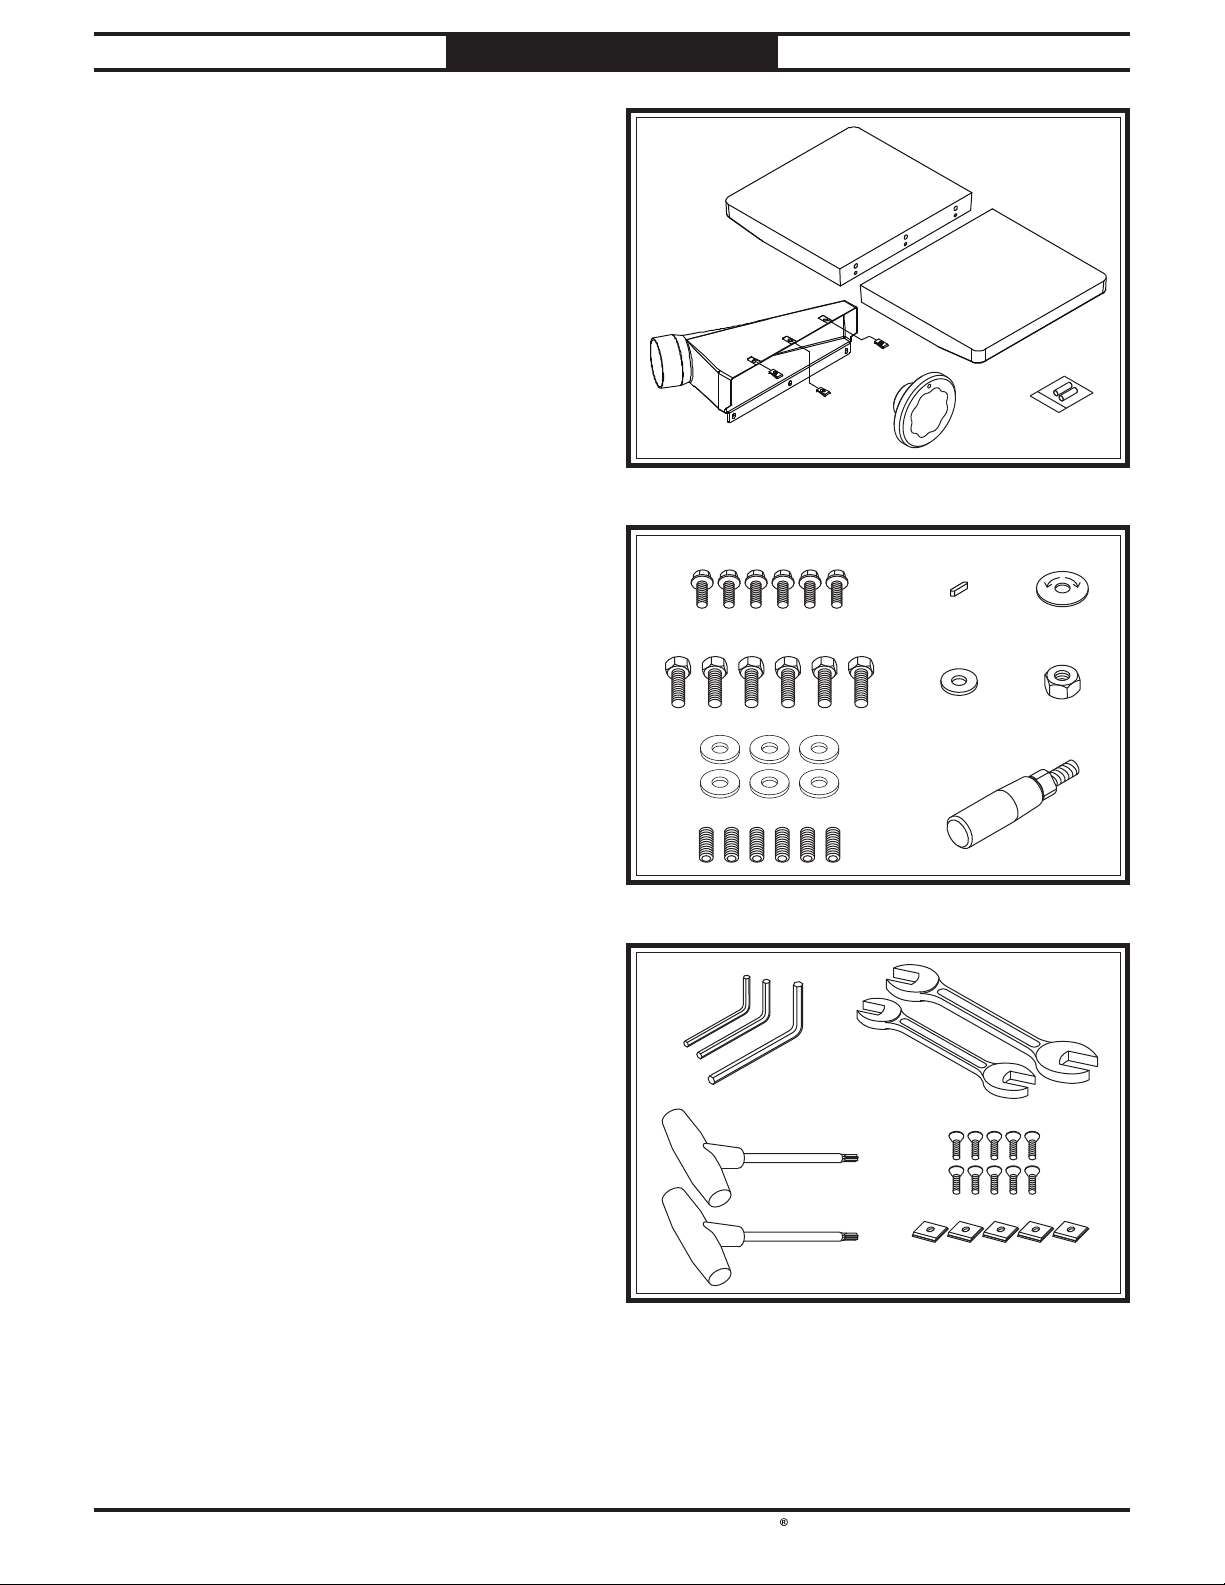
The following is a list of items shipped with your
machine. Before beginning setup, lay these items
out and inventory them.
If any non-proprietary parts are missing (e.g. a
nut or a washer), we will gladly replace them; or
for the sake of expediency, replacements can be
obtained at your local hardware store.
PREPARATION
Unpacking
Inventory
SB1108
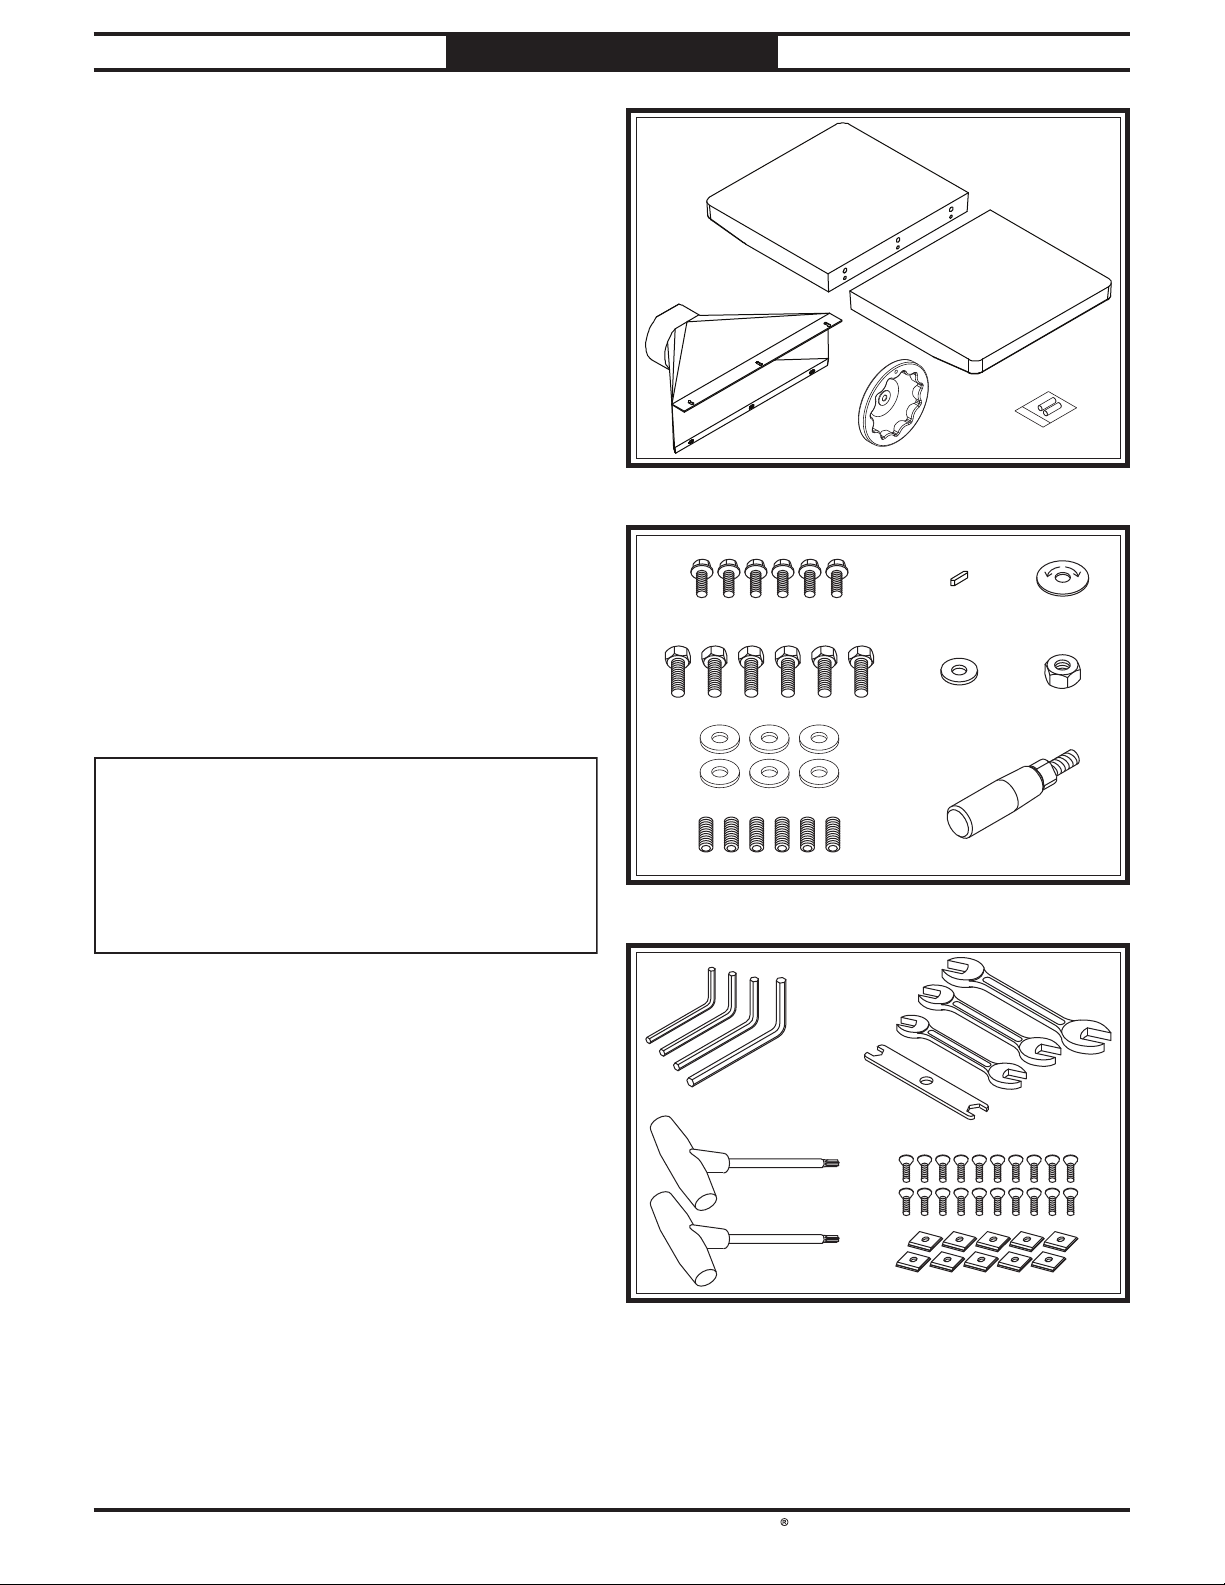
Wood Crate (Figures 6–8) Qty
A. Planer Unit (Not Shown) ............................... 1
Extension Tables ............................................ 2
B.
Dust Hood ....................................................... 1
C.
Handwheel .....................................................1
D.
Batteries AAA ................................................2
E.
Flange Bolts M6-1 x 12 (Dust Port) .............. 6
F.
Machine Key 4 x 4 x 10 (Handwheel) ...........1
G.
Direction Label (Handwheel) ........................ 1
H.
Hex Bolts M8-1.25 x 25 (Ext. Table) ............. 6
I.
Flat Washer 10mm (Handwheel) .................. 1
J.
Hex Nut M10-1.25 (Handwheel) ................... 1
K.
Flat Washers 8mm (Ext. Table) .................... 6
L.
Set Screws M8-1.25 x 12 (Ext. Table) ........... 6
M.
Handwheel Handle ........................................ 1
N.
Hex Wrench Set 3, 4, 6mm ...................1 Each
O.
Open-End Wrench 10/13mm ......................... 1
P.
Open-End Wrench 12/14mm .........................1
T-Handle Torx Wrenches T-25 ...................... 2
Q.
Flat Head Torx Screws #10-32 x 1⁄2" ............ 10
R.
Indexable Carbide Inserts 15 x 15 x 2.5mm . 5
S.
B
C
D E
F G H
I
L
M
O P
Q
J
N
R
S
LOW HIGH
K
-15 -
Page 21
South Bend Tools
Model SB1108/ SB1109
PREPARATION
SB1109
Wood Crate (Figures 9–11) Qty
A. Planer Unit (Not Shown) ............................... 1
Extension Tables ............................................ 2
B.
Dust Hood ....................................................... 1
C.
Handwheel .....................................................1
D.
Batteries AAA ................................................2
E.
Flange Bolts M6-1 x 12 (Dust Hood) ............. 6
F.
Machine Key 4 x 4 x 10 (Handwheel) ...........1
G.
Direction Label (Handwheel) ........................ 1
H.
Hex Bolts M8-1.25 x 25 (Ext. Table) ............. 6
I.
Flat Washer 10mm (Handwheel) .................. 1
J.
Hex Nut M10-1.25 (Handwheel) ................... 1
K.
Flat Washers 8mm (Ext. Table) .................... 6
L.
Set Screws M8-1.25 x 12 (Ext. Table) ........... 6
M.
Handwheel Handle ........................................ 1
N.
Hex Wrench Set 3–6mm .......................1 Each
O.
Open-End Wrench 8/10mm ........................... 1
P.
Open-End Wrench 10/13mm .........................1
Open-End Wrench 12/14mm .........................1
Open-End Wrench 17/19mm .........................1
T-Handle Torx Wrenches T-25 ...................... 2
Q.
Flat Head Torx Screws #10-32 x 1⁄2" ............ 20
R.
Indexable Carbide Inserts 15 x 15 x 2.5mm .10
S.
For Machines Mfd. Since 12/20
B
C
D
E
F G H
I
L
J K
LOW HIGH
NOTICE
If you cannot fi nd an item on this list, carefully
check around/inside the machine and
packaging materials. Often, these items get
lost in packaging materials while unpacking or
they are pre-installed at the factory.
M
O P
Q
S
N
R
-16 -
Page 22
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
The unpainted surfaces are coated
with a heavy-duty rust preventative that
prevents corrosion during shipment and
The benefi t of this rust preventative is that it
works very well. The downside is that it
time-consuming
Be patient and do a careful job when
and removing the rust preventative
you spend doing this will reward you with
smooth
for the proper care of
Although there are many ways to successfully
remove the rust preventative, the
process works well in most situations
Before cleaning, gather the following:
• Disposable
• Cleaner/degreaser
• Safety glasses & disposable gloves
Note:
WD•40 can be used to remove rust preventative.
Before using these products, though, test them
on an inconspicuous area of a painted surface to
make sure they will not damage it.
GAS
PREPARATION
Cleaning & Protecting
at the factory
to thoroughly remove.
-sliding parts and a better appreciation
the unpainted surfaces.
rags
(certain citrus-based
degreasers work extremely well and they
have non-toxic fumes)
Automotive degreasers, mineral spirits, or
. The time
following
storage.
can be
cleaning
.
Avoid chlorine-based solvents, such as
acetone or brake parts cleaner that may
damage painted surfaces. Always follow the
manufacturer’s instructions when using any
type of cleaning product.
Basic steps for removing rust preventative:
1. Put on safety glasses and disposable gloves.
2. Coat all surfaces that have rust preventative
with a liberal amount of your cleaner or
degreaser and let them soak for a few
minutes.
3. Wipe off the surfaces. If your cleaner or
degreaser is effective, the rust preventative
will wipe off easily.
Note: To clean off thick coats of rust
preventative on fl at surfaces, such as beds
or tables, use a PLASTIC paint scraper to
scrape off the majority of the coating before
wiping it off with your rag. (Do not use a
metal scraper or it may scratch the surface.)
4. Repeat Steps 2–3 as necessary until clean,
then coat all unpainted surfaces with a
quality metal protectant or light oil to
prevent rust.
Gasoline and petroleum
products have low flash
points and can explode
or cause fire if used for
cleaning. Avoid using these
products to remove rust
preventative.
Many cleaning solvents are
toxic if inhaled. Minimize
your risk by only using
these products in a well
ventilated area.
T23692—Orange Power Degreaser
A great product for removing the waxy shipping
grease from the non-painted parts of the
machine during clean up.
-17-
Page 23
South Bend Tools
Model SB1108/ SB1109
Weight Load
equipment that may be installed on the machine,
Physical Environment
The physical environment where your machine
is operated is important for safe operation and
longevity of
machine in a dry environment that is free from
excessive moisture, hazardous
chemicals, airborne abrasives, or extreme
conditions. Extreme conditions for this type
of machinery are generally those where the
ambient temperature
104°F; the relative humidity
of
is subject to vibration, shocks, or bumps.
Electrical Installation
Place this machine near an existing power
source. Make sure all power cords are protected
from traffic, material handling, moisture,
chemicals, or other hazards. Make sure to leave
access to a means of disconnecting the power
source or engaging a lockout/tagout device.
Lighting
Lighting around the machine must be adequate
enough to perform operations safely. Shadows,
glare, or strobe effects that may distract or
impede the operator must be eliminated.
PREPARATION
For Machines Mfd. Since 12/20
Location
Physical Environment
Electrical Installation
Lighting
Weight Load
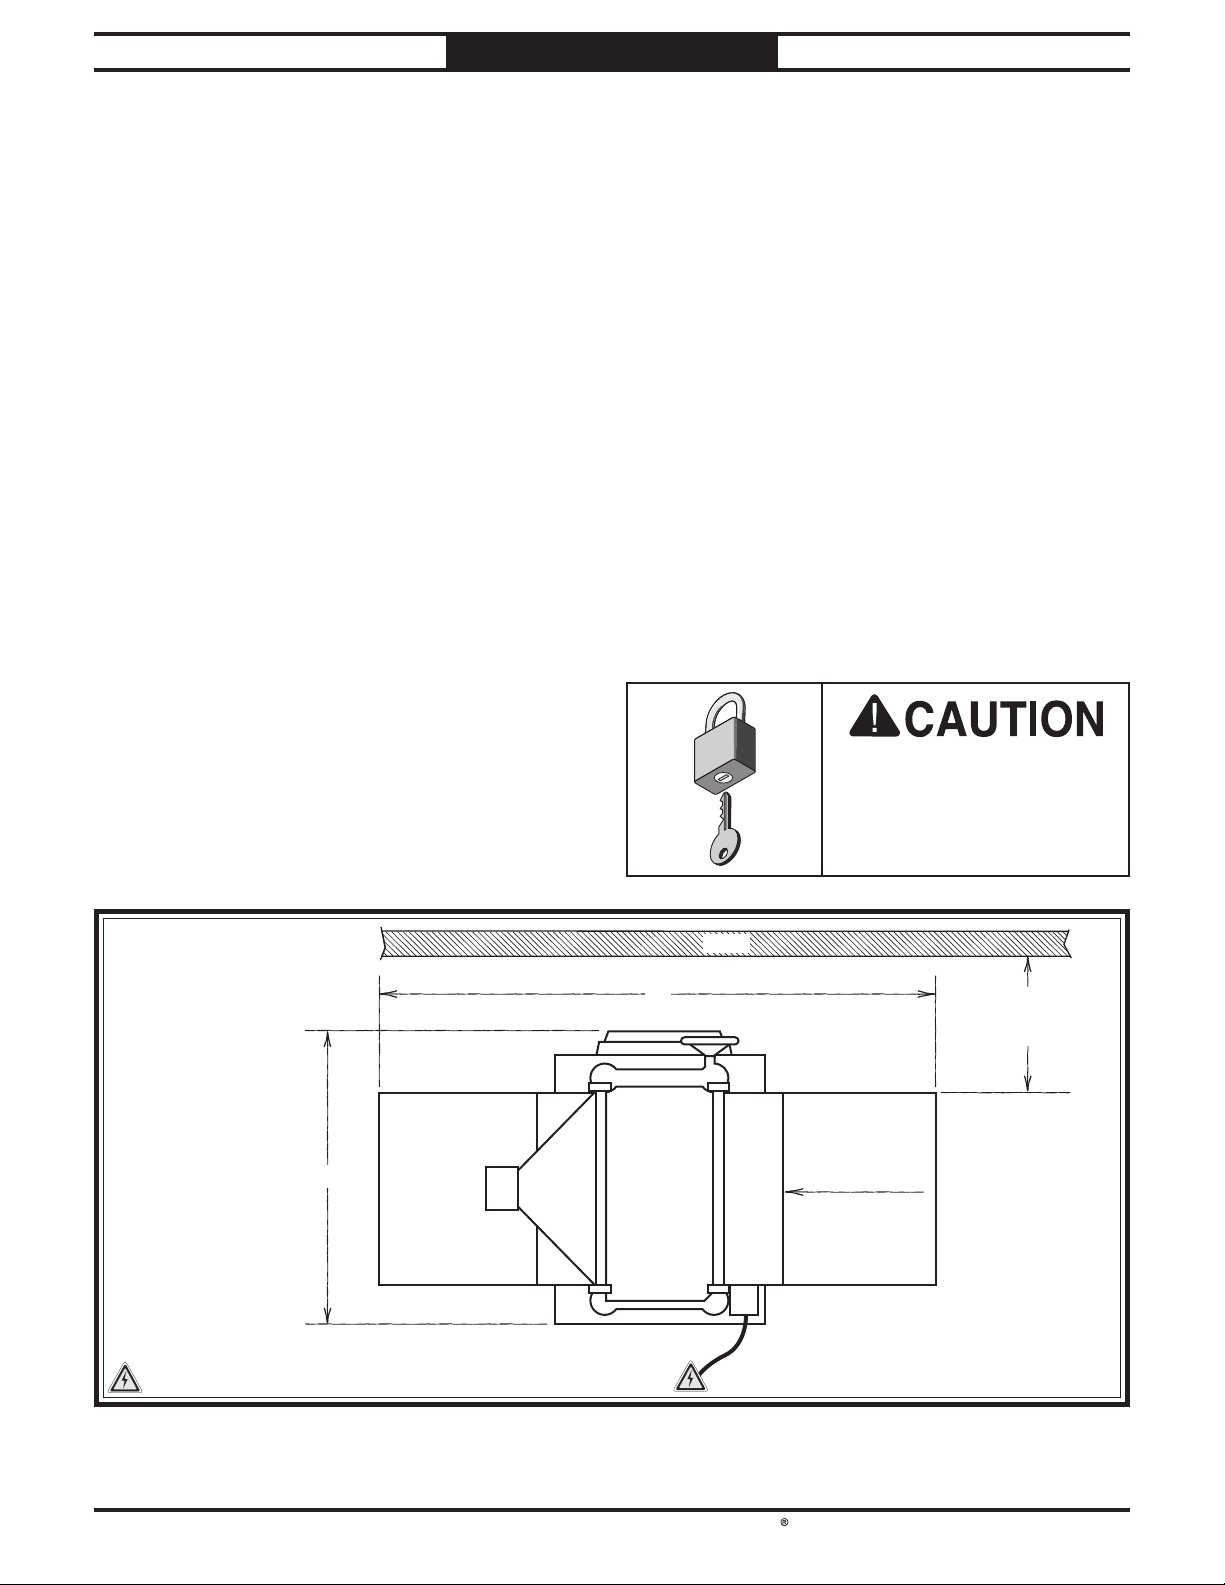
Space Allocation
20–95% (non-condensing); or the environment
parts. For best results, operate this
or flammable
is outside the range of 41°–
is outside the range
Refer to the Machine Specifications for the
weight of your machine. Make sure that the
surface upon which the machine is placed will
bear the weight of the machine, additional
and the heaviest workpiece that will be used.
Additionally, consider the weight of the operator
and any dynamic loading that may occur when
operating the machine.
Space Allocation
Consider the largest size of workpiece that will
be processed through this machine and provide
enough space around the machine for adequate
operator material handling or the installation
of auxiliary equipment. With permanent
installations, leave enough space around
the machine to open or remove doors/covers
as required by the maintenance and service
described in this manual.
Model SB1108
X = 48"
Y = 39"
Model SB1109
X = 56"
Y = 46
1
/2"
Y
Po rt
= Electrical Connection
Children or untrained
people may be seriously
Wall
X
injured by this machine.
Only install in an access
restricted location.
Min. 30"
for Maintenance
Feed DirectionDust
-18 -
Page 24
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PREPARATION
Lifting & Moving
This machine and its
parts are heavy! Serious
personal injury may occur
if safe moving methods are
not used. To reduce the
risk of a lifting or dropping
injury, ask others for help
and use power equipment.
The Models SB1108 and SB1109 require the use
of lifting equipment such as a forklift, engine
hoist, or boom crane. DO NOT attempt to lift or
move planer without necessary assistance from
other people. Each piece of lifting equipment
must be rated for at least 1000 lbs. to support
dynamic loads that may be applied while lifting.
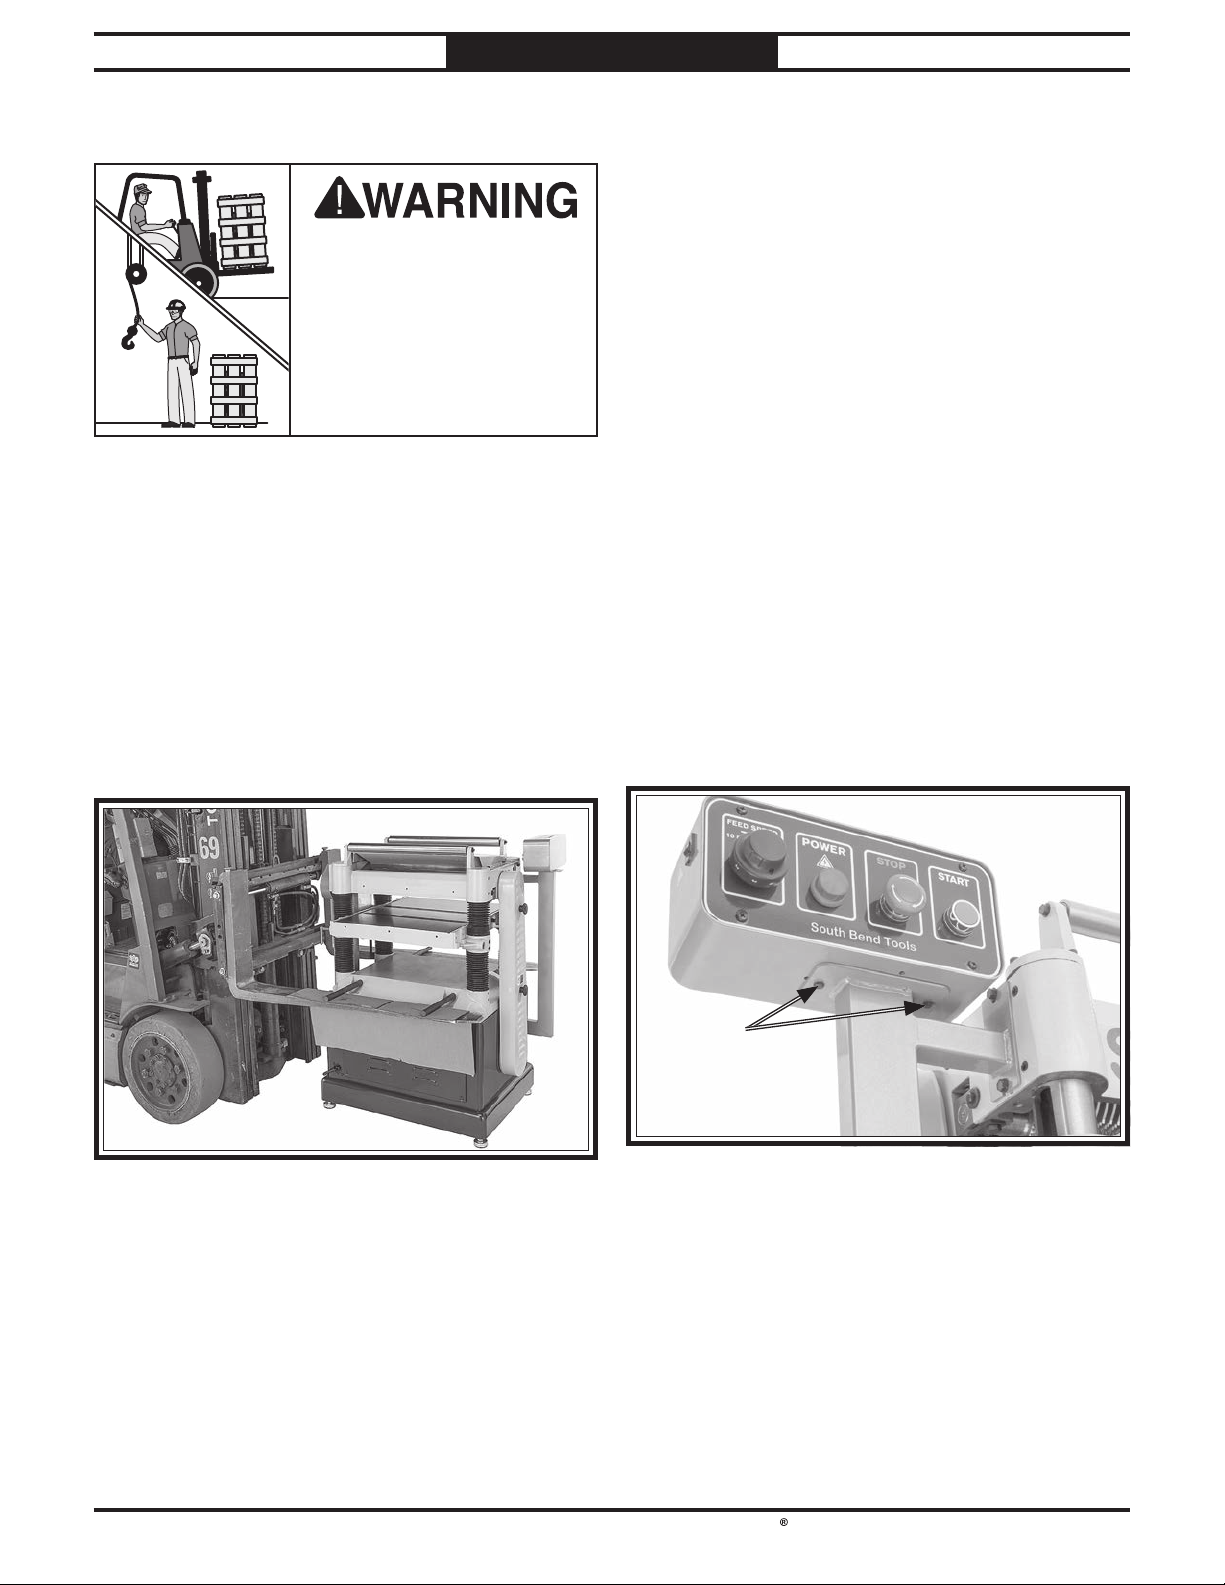
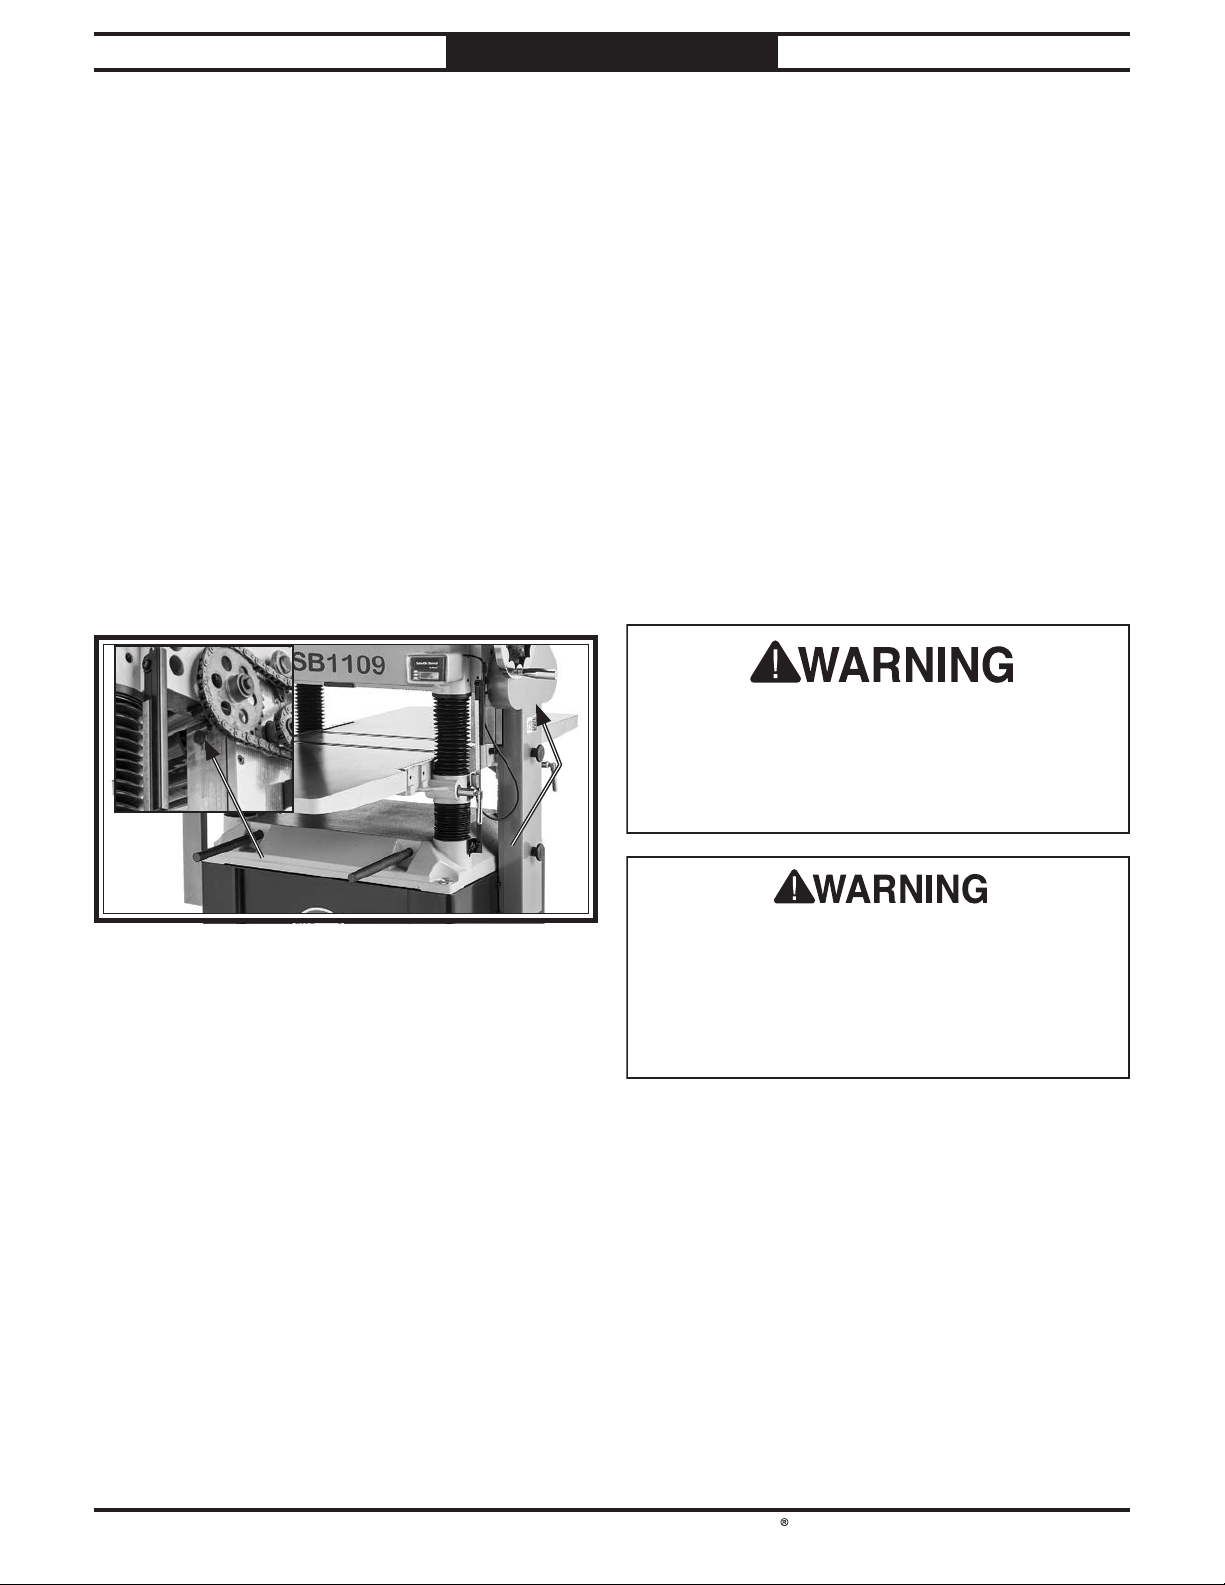
The cabinet stand of your planer is equipped
with four lifting bars that pull out in order to
lift and place the planer as shown in Figure 14
using a forklift or lifting slings.
Assembly
This machine must be fully assembled before it
can be operated. Before beginning the assembly
process, refer to Required for Setup and gather
all listed items. To ensure the assembly process
goes smoothly, first clean any parts that are
covered or coated in heavy-duty rust preventative
(if applicable).
Review the Power Supply section on Page
13, then prepare a permanent location for the
planer.
To assemble planer:
Unbolt planer from pallet.
1.
2. Move planer to desired location.
3. Remove (2) hex bolts from bottom of control
panel (see Figure 15).
Rotate control panel 90° (so front is facing
4.
forward) and install hex bolts removed in
Step 3 (see Figure 15).
Note: When positioning lift forks, place shop rags
or cardboard between the forks and cabinet stand
to avoid scratching the paint.
Control Panel
Mounting Bolts
-19 -
Page 25
South Bend Tools
Model SB1108/ SB1109
LOW HIGH
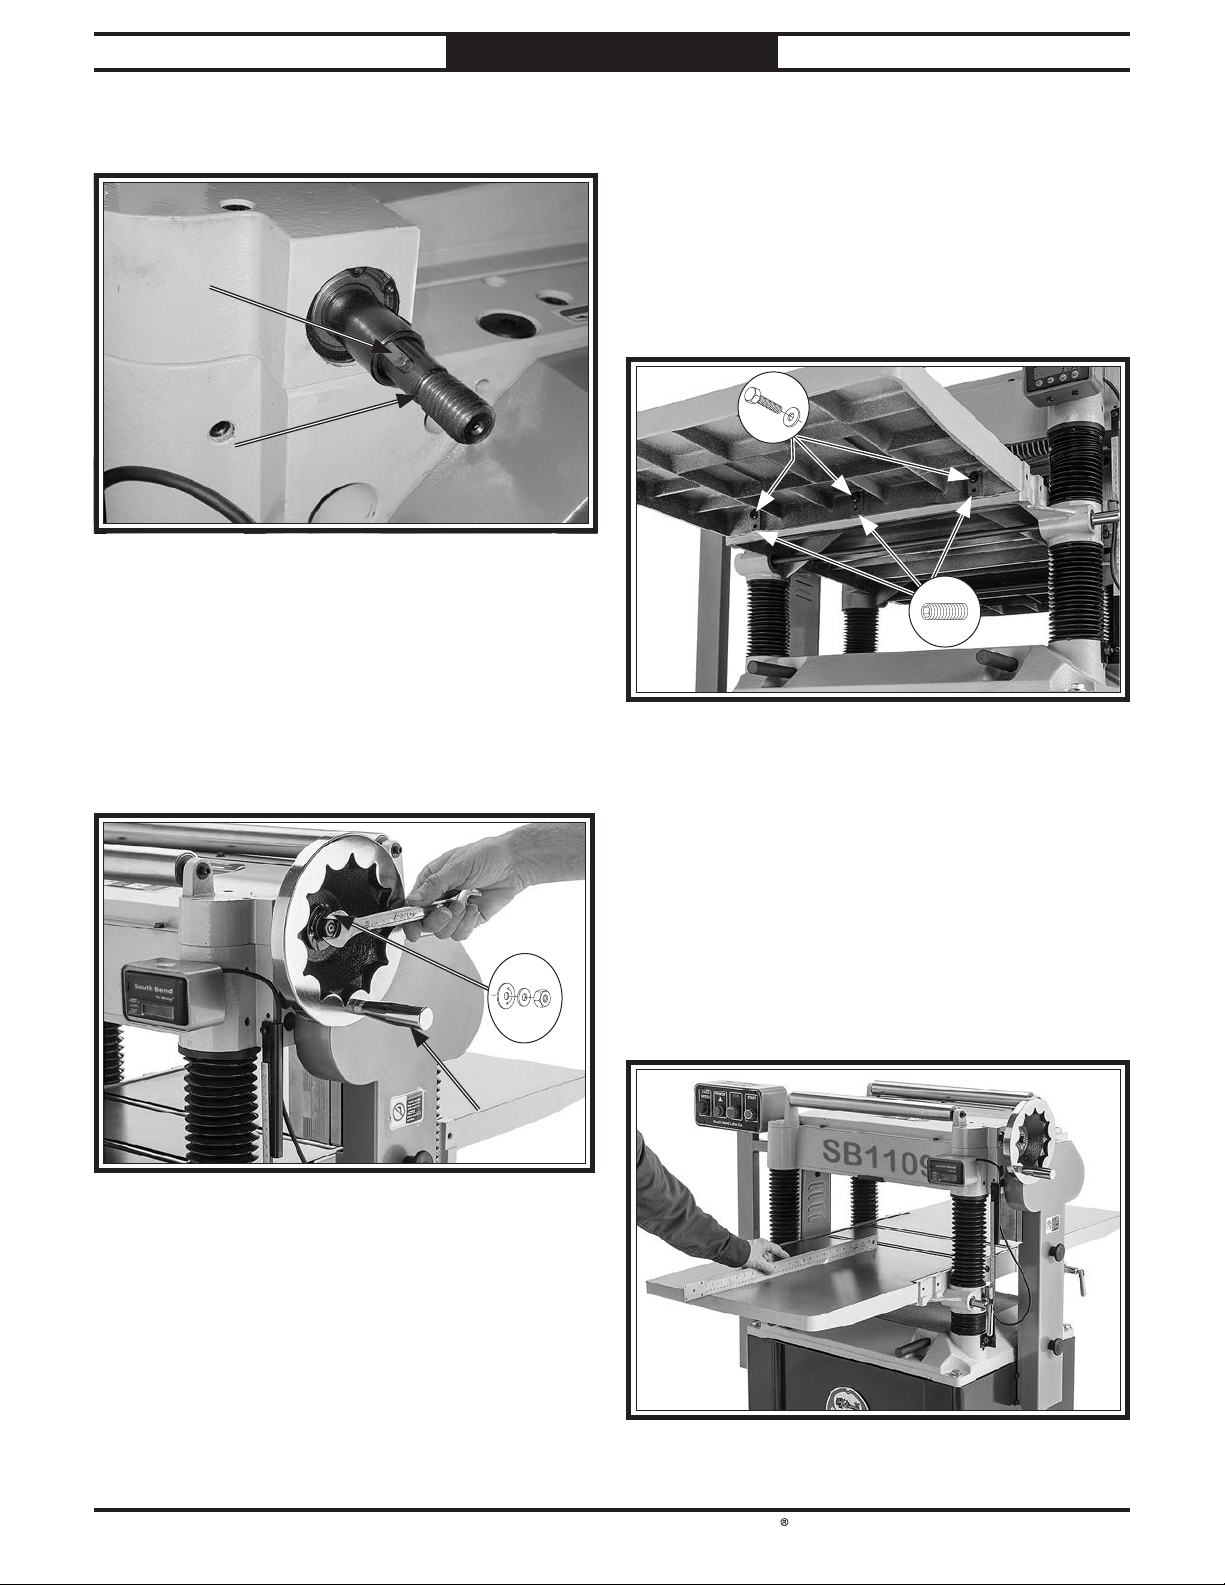
Insert 4 x 4 x 10 key into keyway on
5.
handwheel shaft (see Figure 16).
Line up notch in handwheel bore with
6.
key, slide handwheel onto shaft, then slide
handwheel direction label onto shaft, and
secure with M10-1.75 hex nut and 10mm flat
washer (see Figure 17).
PREPARATION
For Machines Mfd. Since 12/20
8. Attach each cast-iron extension table to
planer table with (3) M8-1.25 x 25 hex
bolts and (3) 8mm flat washers as shown in
Figure 18. Do not fully tighten hex bolts at
this time.
Thread (3) M8-1.25 x 12 set screws into
9.
each extension table at locations shown in
Figure 18.
x 3
x 3
Figure 18. Extension table mounting locations.
7. Thread handle into rim of handwheel and
tighten with wrench (see Figure 17).
Using a straightedge as a guide, rotate
10.
set screws from Step 9 until extension
tables are in plane with main table, then
fully tighten hex bolts from Step 8 (see
Figure 19).
Note: Bed rollers will give you a false reading
if they are raised above table. Move them
down or work around them when leveling
extension wings (refer to Bed Roller Height
on Page 29 for more information).
-20-
Page 26
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PREPARATION
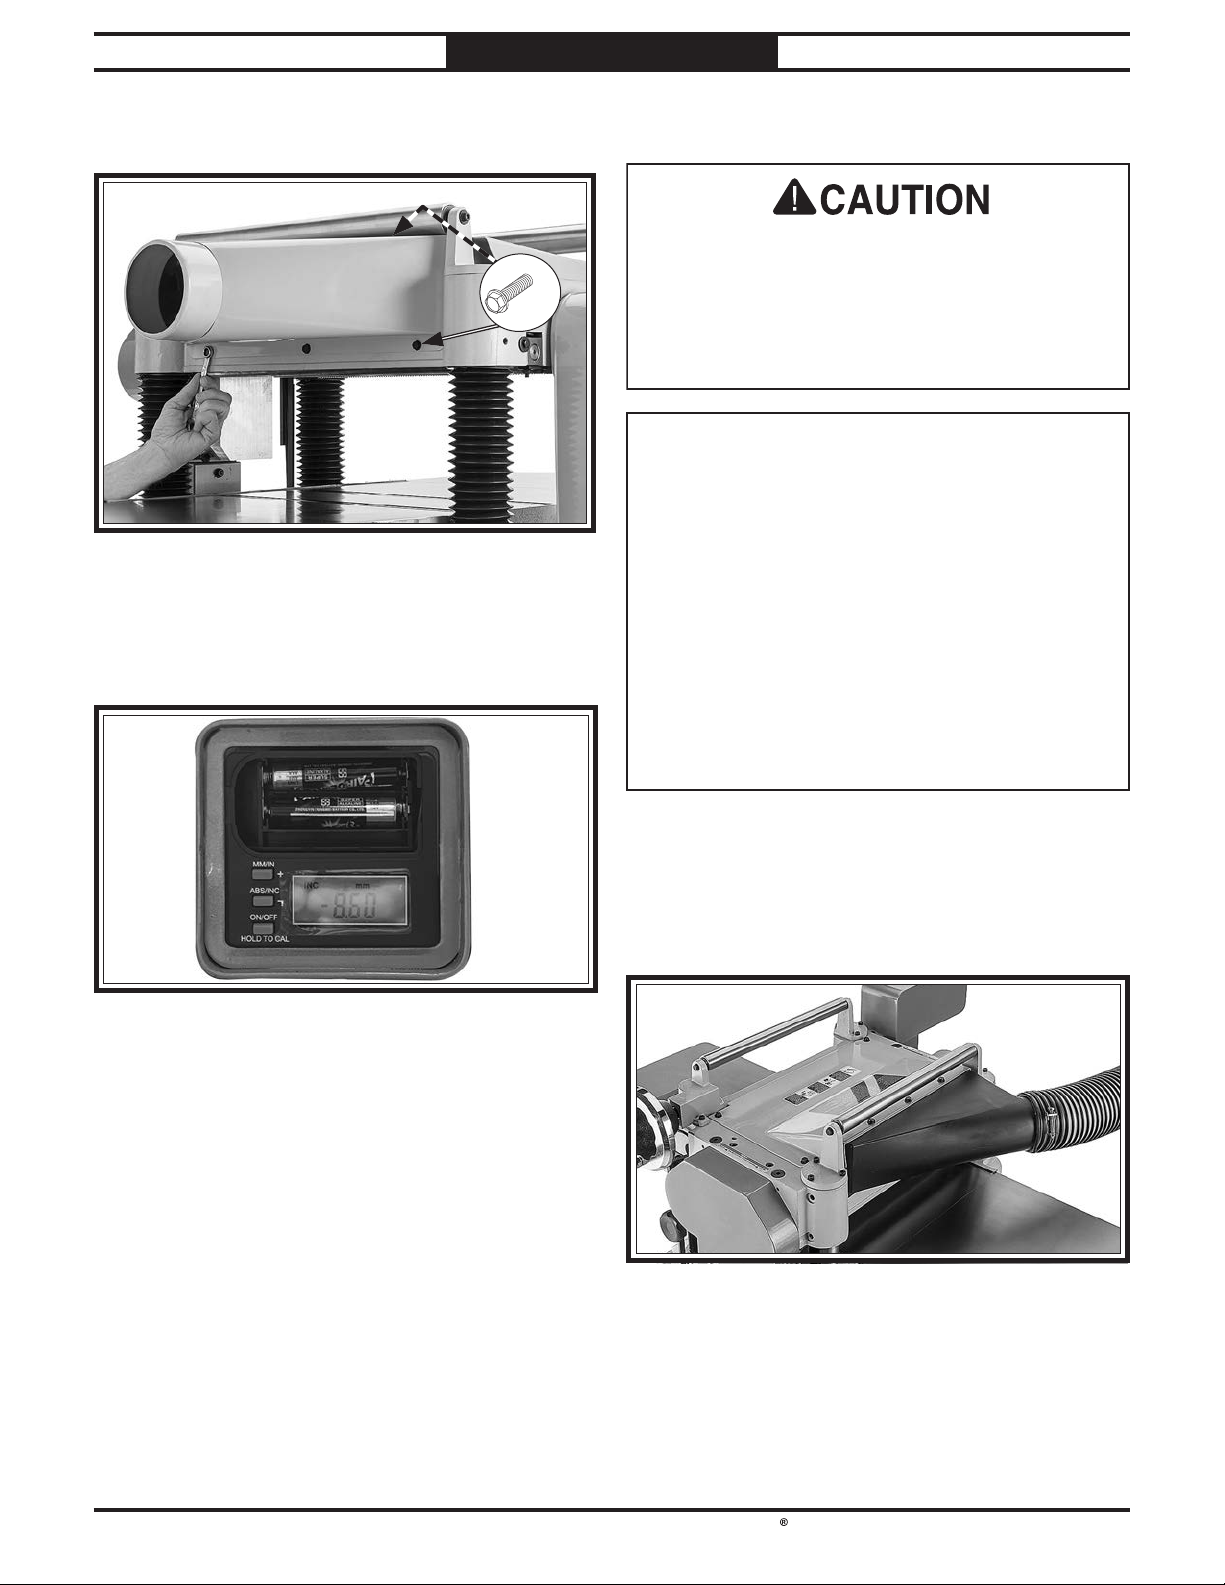
11. Attach dust hood to planer with (6) M6-1 x
12 flange bolts (see Figure 20).
x 6
12. Remove battery cover from front of digital
readout and install (2) AAA batteries (see
Figure 21), then re-install battery cover.
Dust Collection
This machine creates a lot of wood chips/
dust during operation. Breathing airborne dust
on a regular basis can result in permanent
respiratory illness. Reduce your risk by
wearing a respirator and capturing the dust
with a dust-collection system.
Minimum CFM at Dust Port:
• SB1108: 400 CFM
• SB1109: 600 CFM
Do not confuse this CFM recommendation with
the rating of the dust collector. To determine
the CFM at the dust port, you must consider
these variables: (1) CFM rating of the dust
collector, (2) hose type and length between the
dust collector and the machine, (3) number of
branches or wyes, and (4) amount of other open
lines throughout the system. Explaining how to
calculate these variables is beyond the scope of
this manual. Consult an expert or purchase a
good dust collection "how-to" book.
13.
Follow instructions in Calibrating Digital
Readout on Page 31.
To connect machine to a dust collector:
1. For SB1108, fit a 4" dust hose (SB1109
requires 5" dust hose) that is connected to a
dust collector over dust port (see Figure 22),
and secure in place with a hose clamp.
Tug hose to make sure it does not come off.
2.
Note: A tight fit is necessary and ensures
proper performance during operation.
-21-
Page 27
South Bend Tools
Model SB1108/ SB1109
PREPARATION
For Machines Mfd. Since 12/20
Checking Gearbox Oil
gearbox oil level
Level
Before starting your machine for the first time,
check the gearbox oil level. The proper oil level
is just even with the bottom of the fill plug
hole. See Gearbox Oil on Page 37 for more
information. DO NOT mix oil types.
Tools Needed Qty
Open-End Wrench 17mm .....................................1
Hex Wrench 6mm
To check gearbox oil level:
Remove gearbox oil fill plug (see Figure 23).
1.
Note: For easier access to the fill plug, remove
gearbox cover (see Figure 23).
.................................................1
Test Run
After all preparation steps have been completed,
the machine and its safety features must be
tested to ensure correct operation. If you discover
a problem with the operation of the machine or
its safety components, do not operate it further
until you have resolved the problem.
Note: Refer to Troubleshooting on Page 47 for
solutions to common problems that occur with all
planers. If you need additional help, contact our
Tech Support or (360) 734-1540.
The test run consists of verifying the following:
• Motors power up and run correctly.
• EMERGENCY STOP button works
correctly.
Serious injury or death can result from using
this machine BEFORE understanding its
controls and related safety information. DO
NOT operate, or allow others to operate,
machine until the information is understood.
2. Wipe clean 6mm hex wrench and insert
short end inside oil fill hole with inserted
end pointing down, then remove it.
— If end of hex wrench is coated with oil,
then gearbox oil level is okay. Replace fill
plug and continue setup.
— If end of hex wrench is not coated with oil,
then you need to add more oil. Refer to
Gearbox Oil on Page 37 for instructions
on how to do this.
Note: We recommend that you replace the
gearbox oil after the first 20 hours of operation.
This is a normal break-in procedure and will
help maximize the service life of the machine by
flushing away any particles from the break-in
and manufacturing process.
DO NOT start machine until all preceding
setup instructions have been performed.
Operating an improperly set up machine may
result in malfunction or unexpected results
that can lead to serious injury, death, or
machine/property damage.
To test run machine:
1. Clear all tools and objects used during
assembly and preparation away from
machine.
Push EMERGENCY STOP button in.
2.
Connect machine to power supply.
3.
-22-
Page 28
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
Twist EMERGENCY STOP button clockwise
4.
until it pops out (see Figure 24). This resets
switch and machine can now start.
PREPARATION
Inspections & Adjustments
s
i
w
t
T
t
e
s
e
R
o
T
C
l
o
c
k
w
i
z
e
The following list of adjustments were performed
at the factory before your machine was shipped:
• Chip Breaker Height .......................Page 39
• Pressure Bar Height .......................Page 39
• Infeed/Outfeed Roller Height .......Page 39
• Roller Spring Tension ....................Page 42
• Chip Deflector Positioning ............Page 42
• Table Height Chain Tension ........Page 44
• Table Parallelism .............................Page 45
5. Press START button to turn machine ON,
then turn Feed Speed dial from minimum to
maximum. Verify motors start up and run
smoothly without any unusual vibrations or
noises.
— When operating correctly, machine runs
smoothly with little or no vibration or
rubbing noises.
— Investigate and correct strange or
unusual noises or vibrations before
operating machine further. ALWAYS
disconnect machine from power when
investigating or correcting potential
problems.
Press EMERGENCY STOP button to turn
6.
machine OFF.
WITHOUT resetting EMERGENCY STOP
7.
button, try to start machine by pressing
START button. The machine should not
start.
Be aware that machine components can shift
during the shipping process. Pay careful
attention to these adjustments as you test run
your machine. If you find that the adjustments
are not set according to the procedures in this
manual or your personal preferences, re-adjust
them.
After approximately 16 hours of operation,
V-belts will stretch and seat into pulley
grooves and need to be properly tensioned to
ensure good power transfer from motor and
avoid severely reducing life of V-belts. Refer to
Tensioning/Replacing V-Belts on Page 38 for
detailed instructions.
— If machine does not start, the
EMERGENCY STOP button safety
feature is working correctly. Test Run is
complete.
— If machine does start (with EMERGENCY
STOP button pushed in), immediately
disconnect power to machine.
EMERGENCY STOP button safety
feature is not working correctly and must
be replaced before further using the
machine. Call Tech Support for help.
-23-
Page 29
South Bend Tools
Model SB1108/ SB1109
The purpose of this overview is to provide
the novice machine operator with a basic
understanding of how the machine is used during
operation, so they can more easily understand
the controls discussed later in this manual.
Note:
it is not intended to be an instructional guide for
performing actual machine operations. To learn
more about specifi c operations and machining
techniques, seek training from people experienced
with this type of machine, and do additional
research outside of this manual by reading "howto" books, trade magazines, or websites.
OPERATION
For Machines Mfd. Since 12/20
OPERATION
Operation Overview
Due to the generic nature of this overview,
To reduce the risk of
serious injury when using
this machine, read and
understand this entire
manual before beginning
any operations.
To complete a typical operation, the operator
does the following:
1. Examines workpiece to make sure it is
suitable for planing.
Puts on safety glasses or face shield, a
2.
respirator, and hearing protection.
Places workpiece on table with flat side
3.
down and correctly adjusts table height for
workpiece thickness and depth of cut.
— If workpiece is bowed, operator surface
planes workpiece on a jointer, with
cupped side facing down, until one side is
flat. Doing so ensures that it sits solidly
on planer table during operation.
When all safety precautions have been
4.
taken, turns planer ON.
Stands to one side of planer path to reduce
5.
risk of kickback injuries, then feeds
workpiece into planer until infeed roller
grabs it.
To reduce risk of short and
long term injury, wear eye,
ear, and lung protection
when using this machine.
If you are not experienced with this type
of machine, WE STRONGLY RECOMMEND
that you seek additional training outside of
this manual. Read books/magazines or get
formal training before beginning any projects.
Regardless of the content in this section,
South Bend Tools will not be held liable for
accidents caused by lack of training.
Note: Infeed and outfeed rollers control feed
rate of workpiece as it passes through planer.
Operator does not push or pull on workpiece.
— If cut is too deep and bogs down planer,
operator immediately reduces depth of
cut.
Once workpiece is clear of outfeed roller and
6.
stops moving, operator removes workpiece
from outfeed table and measures workpiece
thickness. If further planing is required,
operator raises table slightly, such as
of table height handwheel (approximately
1
⁄4 to 1⁄2 turn of the handwheel), then feeds
workpiece into front of planer again.
Operator continues process until desired
7.
workpiece thickness is achieved, then turns
machine OFF.
1
⁄2-turn
-24-
Page 30
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
South Bend Tools
Some workpieces are not safe to use or may
require modifi cation before they are.
planing, inspect all workpieces for the following:
•
•
•
cause kickback and machine damage. Always
•
the machine. Excess moisture can also hasten
•
•
facing the table. On the contrary, a workpiece
The species of wood, as well as its condition,
greatly affects the depth of cut the planer can
effectively take with each pass.
The chart below shows the Janka Hardness
Rating for a number of commonly used species.
The larger the number, the harder the workpiece,
and the less material should be removed in any
one pass for good results.
Note:
The Janka Hardness Rating is expressed in
pounds of force required to embed a 0.444" steel
ball into the surface of the wood to a depth equal
to half the ball's diameter.
OPERATION
Wood TypesStock Inspection &
Stock Inspection
Requirements
Before
Material Type: This machine is only
intended for workpieces of natural wood
fi ber Attempting to use workpieces of any
other material that may break apart during
operation could lead to serious personal
injury and property damage.
Foreign Objects: Inspect lumber for defects
and foreign objects (nails, staples, embedded
gravel, etc,). If you have any question about
the quality of your lumber, DO NOT use it.
Remember, wood stacked on a concrete floor
can have small pieces of stone or concrete
pressed into the surface.
Large/Loose Knots: Loose knots can become
dislodged during operation. Large knots can
use workpieces that do not have large/loose
knots.
Wet or "Green" Stock: Avoid using wood with
a high water content. Wood with more than
20% moisture content or wood exposed to
excessive moisture (such as rain or snow),
will cut poorly and cause excessive wear to
Janka
Species
Hardness
Ebony 3220
Red Mahogany 2697
Rosewood 1780
Red Pine 1630
Sugar Maple 1450
White Oak 1360
White Ash 1320
American Beech 1300
Red Oak 1290
Black Walnut 1010
Teak 1000
rust and corrosion of the machine and/or
individual components.
Excessive Warping: Workpieces with
excessive cupping, bowing, or twisting are
dangerous to cut because they are unstable
and often unpredictable when being
cut. DO NOT use workpieces with these
characteristics!
Minor Cupping: Though it is always best to
fl atten the cupped side on a jointer before
planing, workpieces with slight cupping
can be safely supported if the cupped side is
supported on the bowed side will rock during
operation and could cause severe injury from
kickback.
Black Cherry 950
Cedar 900
Sycamore 770
Douglas Fir 660
Chestnut 540
Hemlock 500
White Pine 420
Basswood 410
Eastern White Pine 380
Balsa 100
-25-
Page 31
South Bend Tools
Model SB1108/ SB1109
• Inspect your lumber for twisting or cupping,
•
•
•
•
•
• Use a jointer on one side of the workpiece and
•
knives/inserts will remain sharp much longer.
•
• Plane ONLY natural wood fiber. Do not plane
wood composites or other materials that could
•
Below is a list of wood characteristics you
may encounter when planing. The following
descriptions of defects will give you some possible
answers to problems you may encounter while
planing different materials. Possible solutions
follow the descriptions.
Chipped Grain
Problem:
grain, planing lumber with knots or excessive
amount of cross grain, or using dull knives/
inserts.
Note:
highly fi gured wood.
Solution:
feed rate. Inspect your lumber and determine if
its grain pattern is causing the problem. If the
lumber does not show substantial crossgrain,
inspect your knives/inserts.
Fuzzy Grain
Problem:
with too high of a moisture content. Sometimes
fuzzy grain is an unavoidable characteristic of
some woods, such as basswood. Fuzzy grain can
also be caused by dull knives/inserts.
Solution:
meter. If moisture is greater than 20%, sticker
the lumber and allow it to dry. Otherwise,
inspect the knife/insert condition.
OPERATION
For Machines Mfd. Since 12/20
Planing Tips
and surface cupped side on a jointer if
necessary before planing workpiece.
Scrape off all glue when planing glued-up
panels. Dried glue can quickly dull inserts.
DO NOT plane more than one piece at a time
side by side.
Never remove more than the recommended
amount of material on each pass. Only
remove a small amount of material on each
pass when planing wide or dense stock.
Support the workpiece on both ends. Get
assistance from another person if you are
planing long lumber, or use roller stands to
support the workpiece.
Measure the workpiece thickness with
calipers to get exact results.
the planer for the other.
Use the entire width of the planer to
wear knives/inserts evenly. With narrow
workpieces, alternate between far left, far
right, and the middle of the table. Your
To avoid "chip marks", always plane WITH
the grain direction of the wood. Never plane
cross-grain or end-grain.
Common Cutting Problems
Usually a result of cutting against the
Some amount of chipping is normal with
Decrease the depth of cut. Reduce the
Usually caused by surfacing lumber
Check the lumber with a moisture
break up in the planer and cause operator
injury or damage to planer.
Always true cupped or warped stock on a
jointer before planing.
-26-
Page 32
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
Pitch & Glue Build-up
Problem:
and cutterhead will cause overheating by
decreasing cutting sharpness while increasing
drag in the feed mechanism. The result can
include scorched lumber, uneven knife/insert
marks, and chatter.
Solution:
Chip Marks or Indentations
Problem:
the result of wood chips not being thrown away
from the cutterhead and out of the machine.
Instead they are carried around the cutterhead,
deposited on the planed surface and crushed by
the outfeed roller. Some of the causes of chip
indentation are:
•
•
•
•
Solution:
•
•
moisture. DO NOT surface partially-air-dried
•
•
Snipe
Problem:
material removed than the rest of the board.
Usually caused when the workpiece is not
properly supported as it goes through the
machine. In many cases, however, a small
amount of snipe is inevitable and cannot be
completely prevented.
Solution:
the outfeed end of the planer. The best way to
deal with snipe is by planing lumber longer than
your intended work length and then cutting off
the excess after planing is completed.
Rippled Cut
Problem:
face of workpiece are caused by excessive outfeed
roller pressure or excessive feed rate.
Solution:
feed rate.
OPERATION
Glue and resin buildup on the rollers
Clean the rollers and cutterhead.
Chip indentation or chip bruising is
Wood chips/sawdust not being properly
expelled from the cutterhead.
The type of lumber being planed. Certain
species have a tendency to chip bruise.
Dull knives/inserts.
Excessive depth of cut.
Use a proper dust-collection system; adjust
chip defl ector in or out as necessary.
Occurs when board ends have more
Hold workpiece up slightly as it leaves
Regularly spaced indentations across
Reduce outfeed roller pressure; reduce
Lumber must be completely dry, preferably
kiln-dried (KD). Air-dried (AD) lumber must
be seasoned properly and have no surface
(PAD) lumber.
Make sure planer knives/inserts are sharp.
Reduce depth of cut.
-27-
Page 33
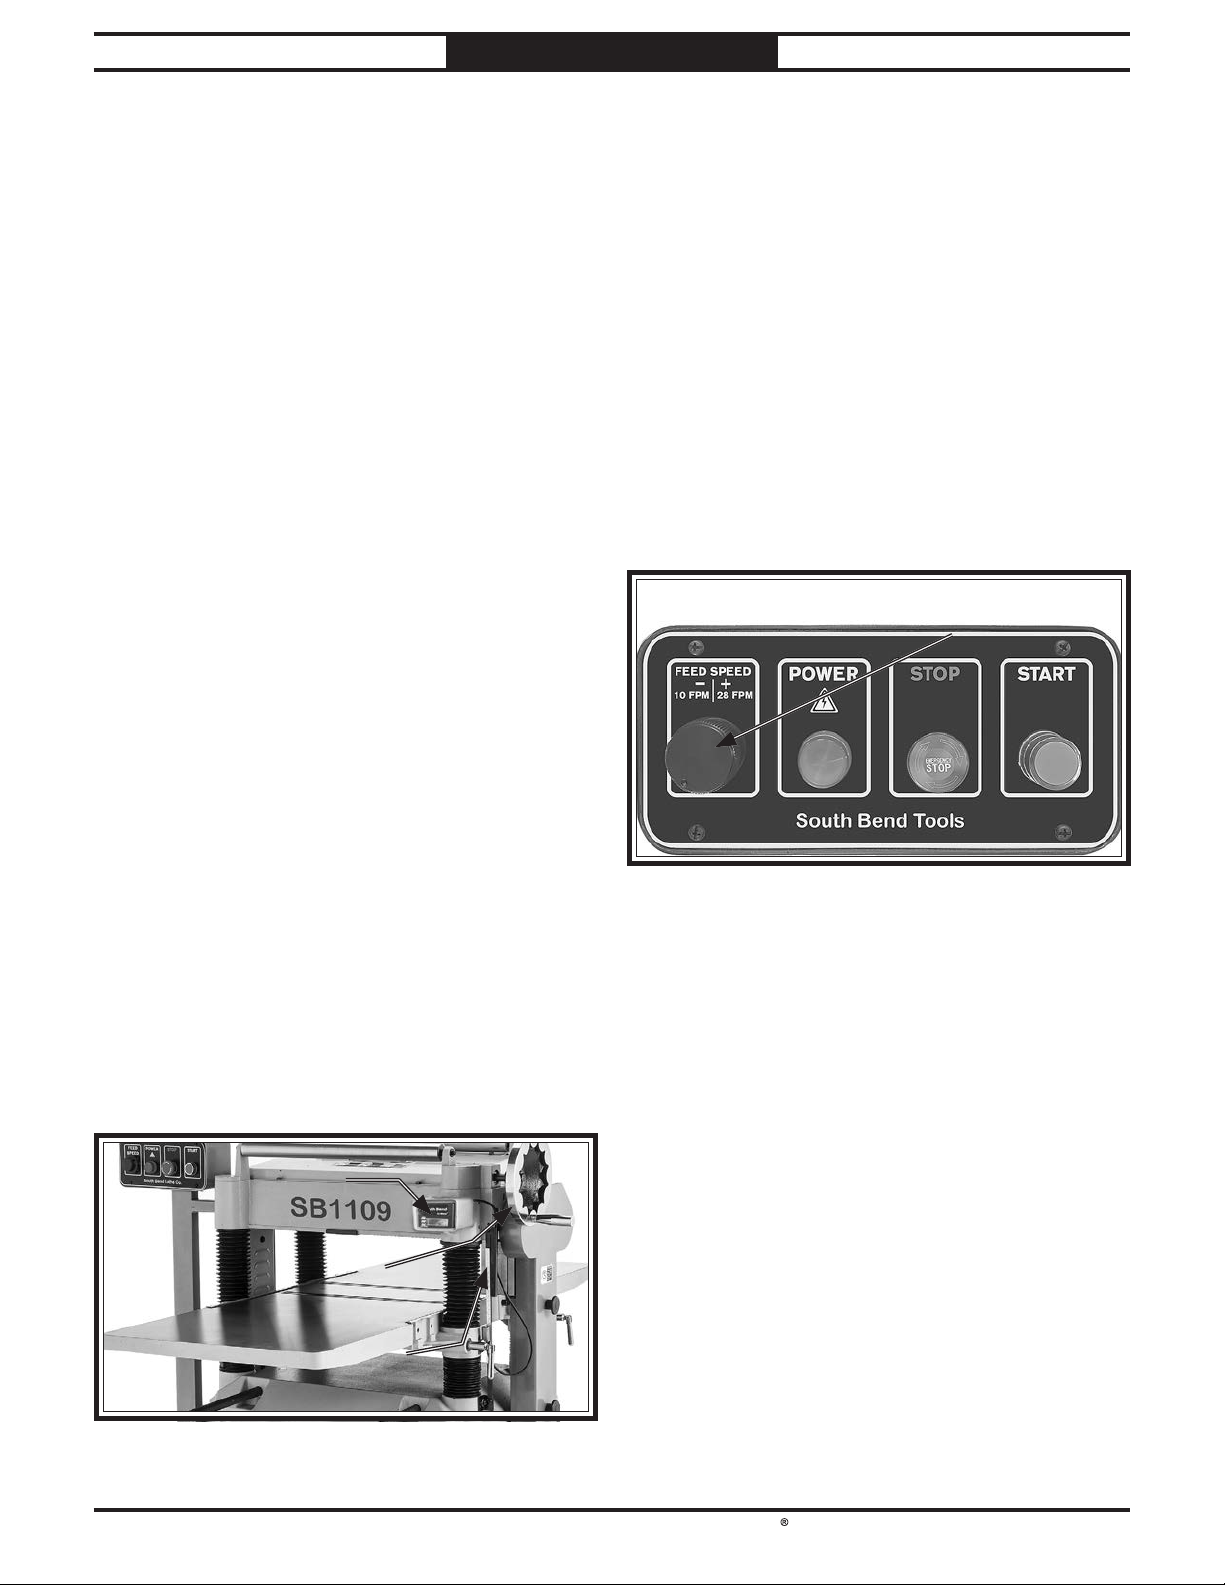
South Bend Tools
Model SB1108/ SB1109
OPERATION
For Machines Mfd. Since 12/20
Depth of Cut
Table Movement
One Full Revolution of Handwheel
Material Thickness Range
SB1108
SB1109
The depth of cut on a planer means the amount
of material that is removed from the top of
the workpiece as it passes underneath the
cutterhead.
The depth of cut is set by adjusting the distance
of the table below the cutterhead. This distance
is the thickness of the workpiece minus the depth
of cut. The planing depth of cut is controlled by
using the table height handwheel on the right
side of the machine. Rotating the handwheel
clockwise raises the table.
Although the correct depth of cut varies
according to wood hardness and workpiece width,
we recommend the maximum depth of cut (per
pass) be no more than
will give better end results and put less stress
on the planer than trying to take off too much
material in a single pass.
.......................................................3/16"
.........................................................1⁄4" – 8"
1
Depth of Cut
..................1⁄16"
—
⁄16". A series of light cuts
6"
Setting Feed Rate
Feed Rate ..............................................10–28 FPM
The infeed and outfeed rollers move the
workpiece through the planer while keeping it
flat and providing a consistent rate of movement.
The speed that these rollers move the workpiece
through the planer is the feed rate.
Generally, low feed rates are used for finishing
passes, while higher feed rates are used for
dimensioning passes.
Use the FEED SPEED control knob (see
Figure 26) to adjust the feed rate according
workpiece type and desired results.
Feed Rate
The depth of cut can be referenced directly from
the scale on the front of the planer, as shown in
the figure below.
Note: The scale and digital readout function as a
general guide only, and is not intended for lowtolerance, precision results. To ensure accuracy,
use a tape measure or caliper to measure your
workpiece thickness after each pass.
Figure 26. Feed speed control knob.
-28-
Page 34
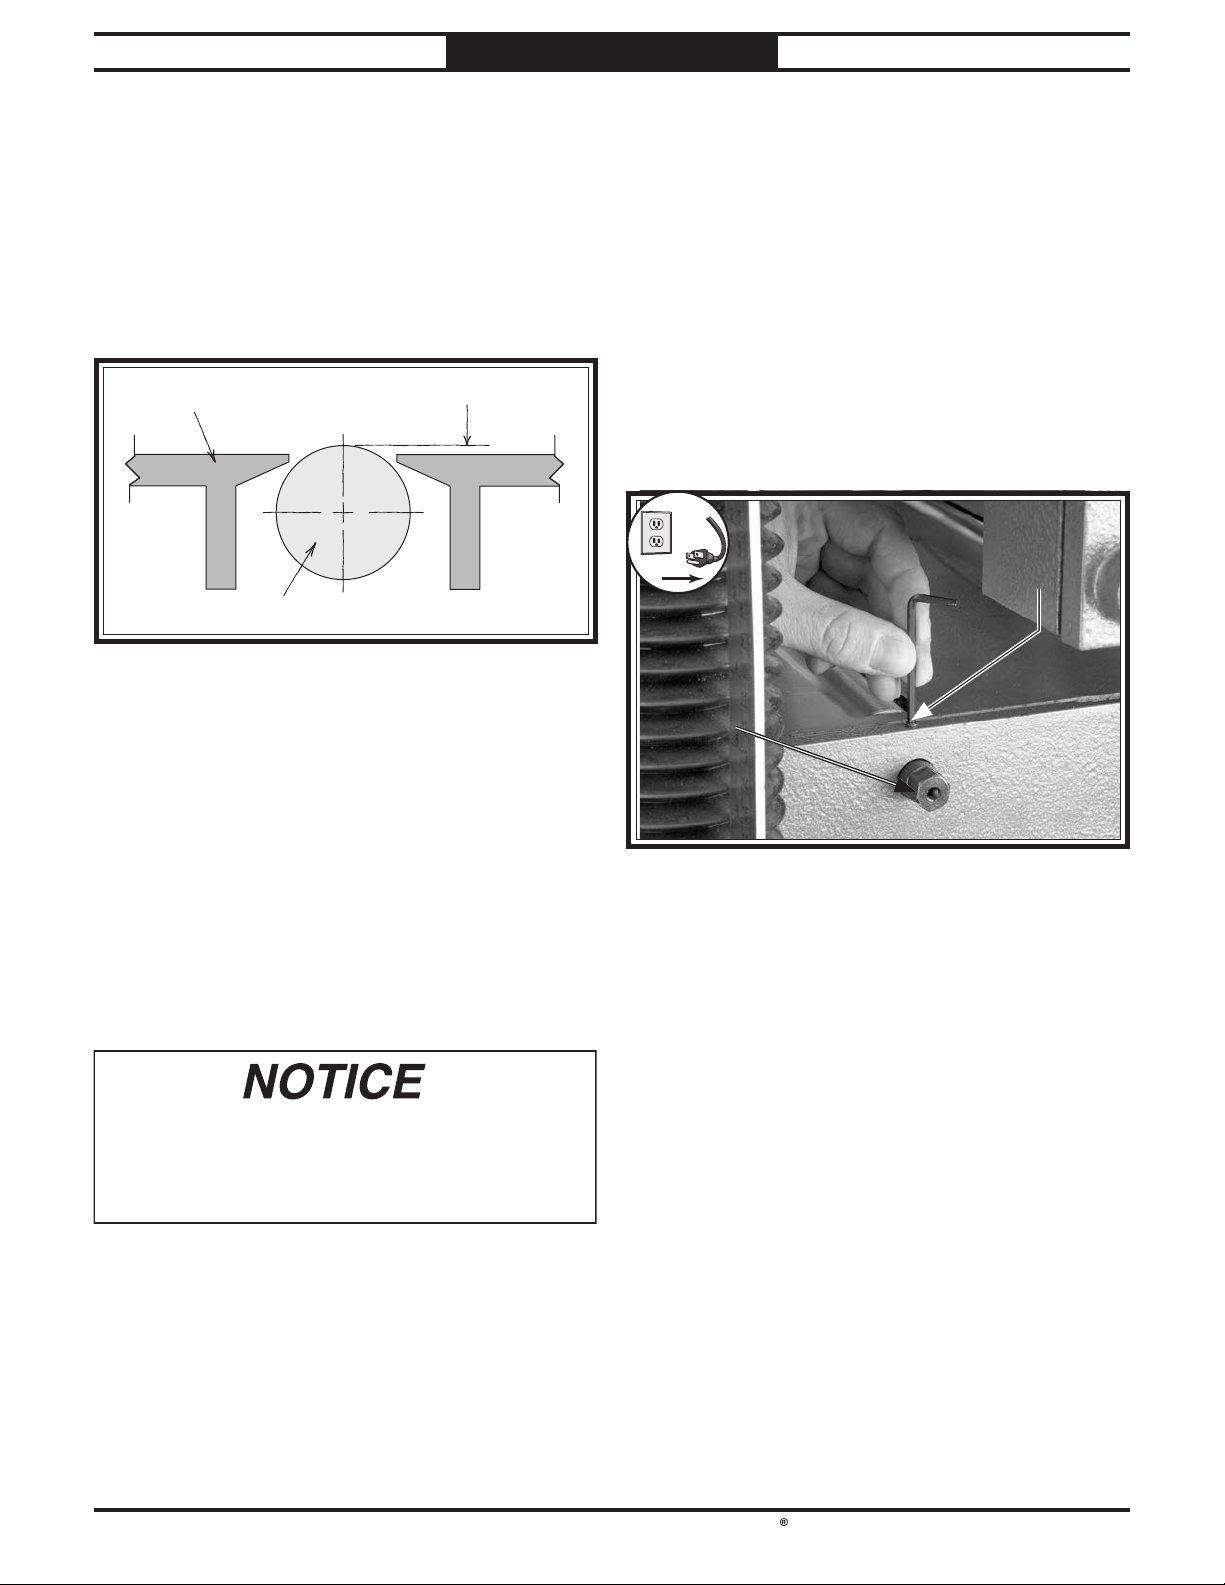
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
The correct height of the bed rollers will vary,
depending on the type of material you intend to
plane. However, as a general rule, keep the bed
roller height range within the listed range above
the table surface, as illustrated.
When planing rough stock, set the rollers high
to keep the lumber from dragging along the bed.
When planing milled lumber, set the rollers low
to help minimize snipe.
To ensure accurate results and make the
adjustment process quicker and easier,
we recommend using a Rotacator (refer to
Accessories) to gauge the bed roller height from
the table surface. If a Rotacator is not available,
a straightedge and feeler gauges can be used, but
!
OPERATION
Bed Roller Height
Bed Roller Height Range ................. 0.002"–0.020"
Table
Roller
Bed Roller Height
0.002"–0.020"
Items Needed Qty
Hex Wrench 3mm .................................................1
Open-End Wrench 14mm
Rotacator (optional, see Page 32)
.....................................1
........................ 1
To adjust bed roller height:
1. DISCONNECT MACHINE FROM POWER!
2. Completely lower table to give yourself
enough room to work.
Loosen set screw above each of four roller
3.
adjustment cams—there are two on each
side of planer table (see Figure 28).
Bed rollers that are not adjusted to the correct
height or out of alignment with each other
can cause poor fi nishes, inconsistent planing
thickness, and other undesirable results.
Rotate eccentric adjustment cams on each
4.
side of roller to raise or lower bed rollers to
desired height above table surface.
Verify both sides of each roller are at the
5.
same height, then re-tighten set screws to
secure in place.
IMPORTANT: Bed rollers MUST be parallel
with the table.
Re-check roller heights to make sure they
6.
did not change while being secured.
— If roller heights are not correct, repeat
this procedure until they are.
-29-
Page 35
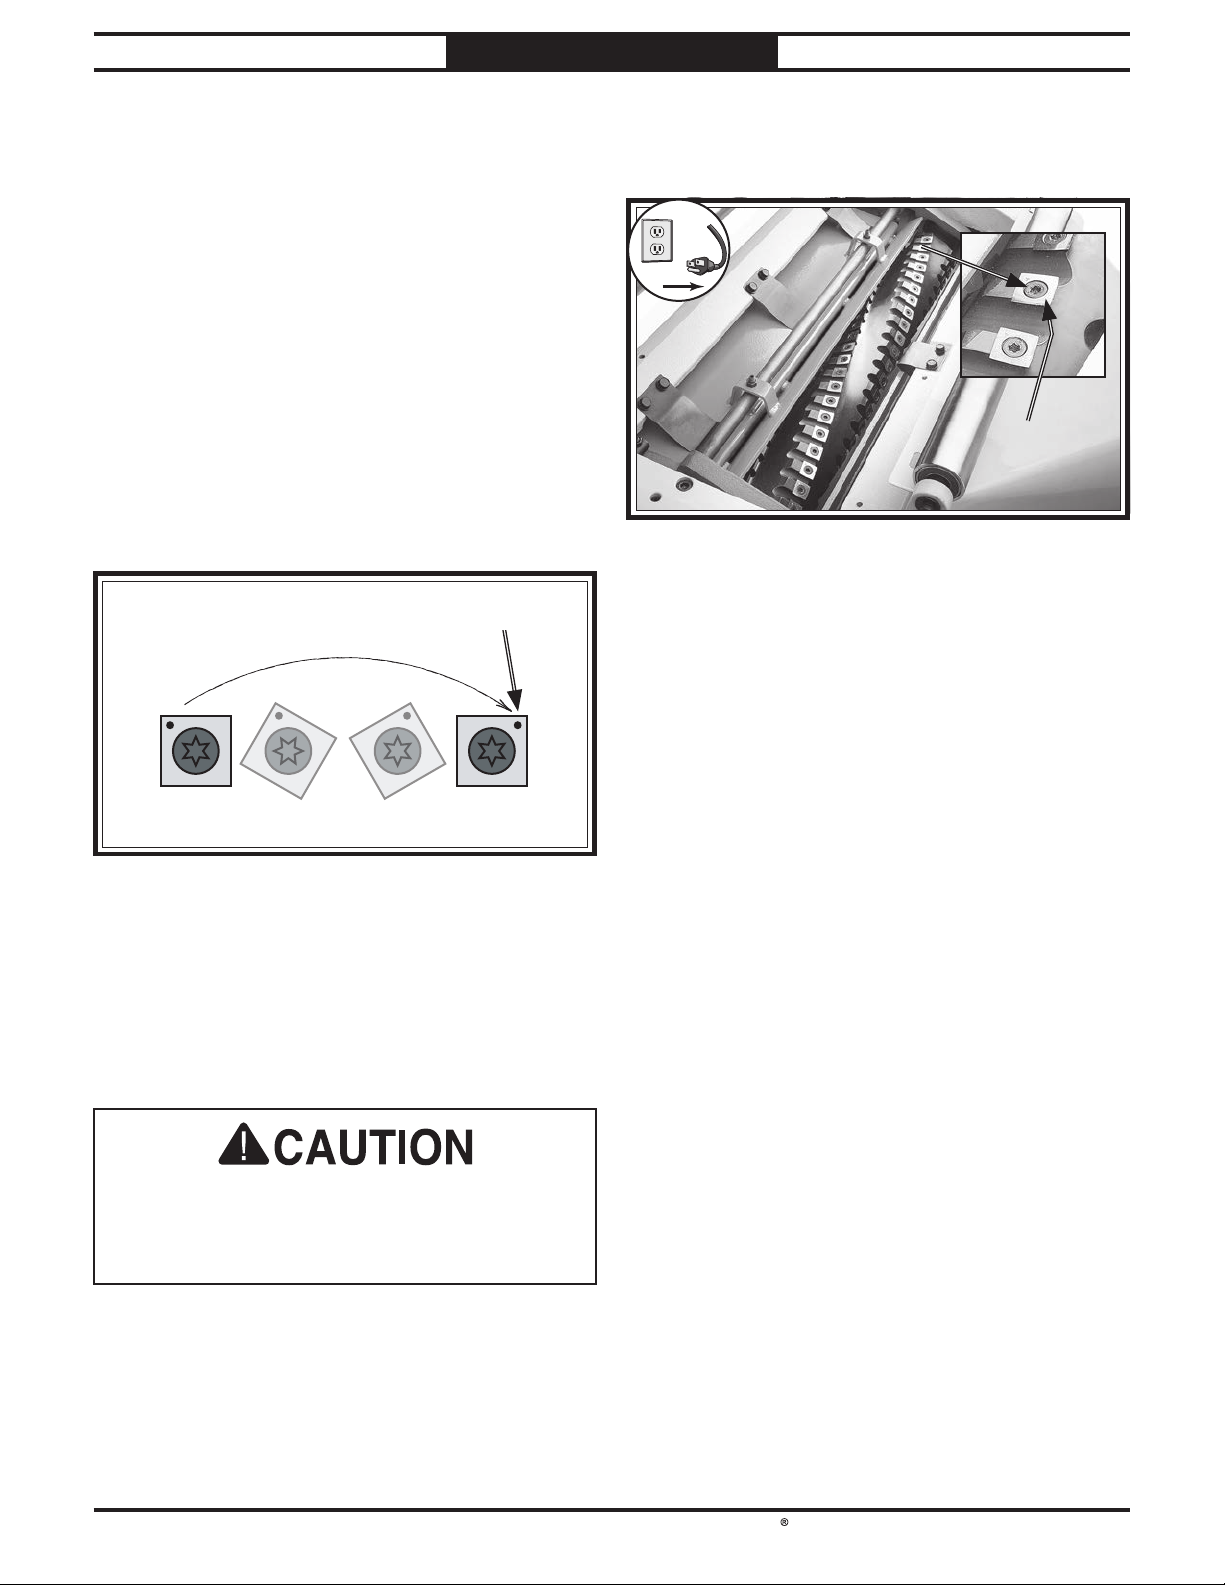
South Bend Tools
Model SB1108/ SB1109
The spiral cutterhead is equipped with 4-sided
indexable carbide inserts. Each insert can be
removed, rotated, and re-installed to use any one
of its four cutting edges. Therefore, if one cutting
edge becomes dull or damaged, simply rotate it
90˚ (as shown below) to use a sharp cutting edge.
The inserts have a reference dot on one corner.
The position of the reference dot on installed
inserts can be used to track which edges are
sharp/unused and which edges are dull or
damaged. Replace inserts once the reference dot
has been rotated back to its original position.
!
OPERATION
For Machines Mfd. Since 12/20
Rotating/Replacing
Cutterhead Inserts
Cutterhead Inserts
Reference Dot
3. Remove any sawdust or debris from head
of insert, Torx screw, and surrounding area
(see Figure 30).
4. Remove Torx screw and insert, then clean
all dust and debris from both parts and
cutterhead pocket.
Items Needed Qty
Hex Wrench 5mm .................................................1
Wrench or Socket 10mm
T-25 Torx Bit
Carbide Cutterhead Inserts.................. As Needed
...................................................... As Needed
Rags
Light Machine Oil
The carbide inserts are very sharp and can
quickly cut your hands. ALWAYS use caution
when handling these parts to reduce the risk
of personal injury.
......................................................... 1
................................. As Needed
....................................... 1
Note: Proper cleaning of insert, Torx screw,
and cutterhead pocket is critical to achieving
a smooth finish. Dirt or dust trapped between
insert and cutterhead will raise insert,
and make marks on your workpiece when
planing.
Tip: Use low-pressure compressed air or a
vacuum nozzle to clean out cutterhead pocket.
Replace insert so that a fresh cutting edge
5.
faces outward.
— If all four insert cutting edges have been
used, replace insert with a new one.
Always position insert reference dot in
same position when installing a new
insert to aid in rotational sequencing.
Lubricate Torx screw threads with a very
6.
small amount of light machine oil, wipe
excess off, and torque screw to 50–55 inch/
pounds.
To rotate or replace a helical cutterhead
insert:
1. DISCONNECT MACHINE FROM POWER!
2. Remove dust hood, top cover, and belt cover.
-30-
Note: If too much oil is applied to the
threads, excess oil will attempt to squeeze
out of the threaded hole and raise insert
during installation, bringing it out of height
alignment.
Page 36
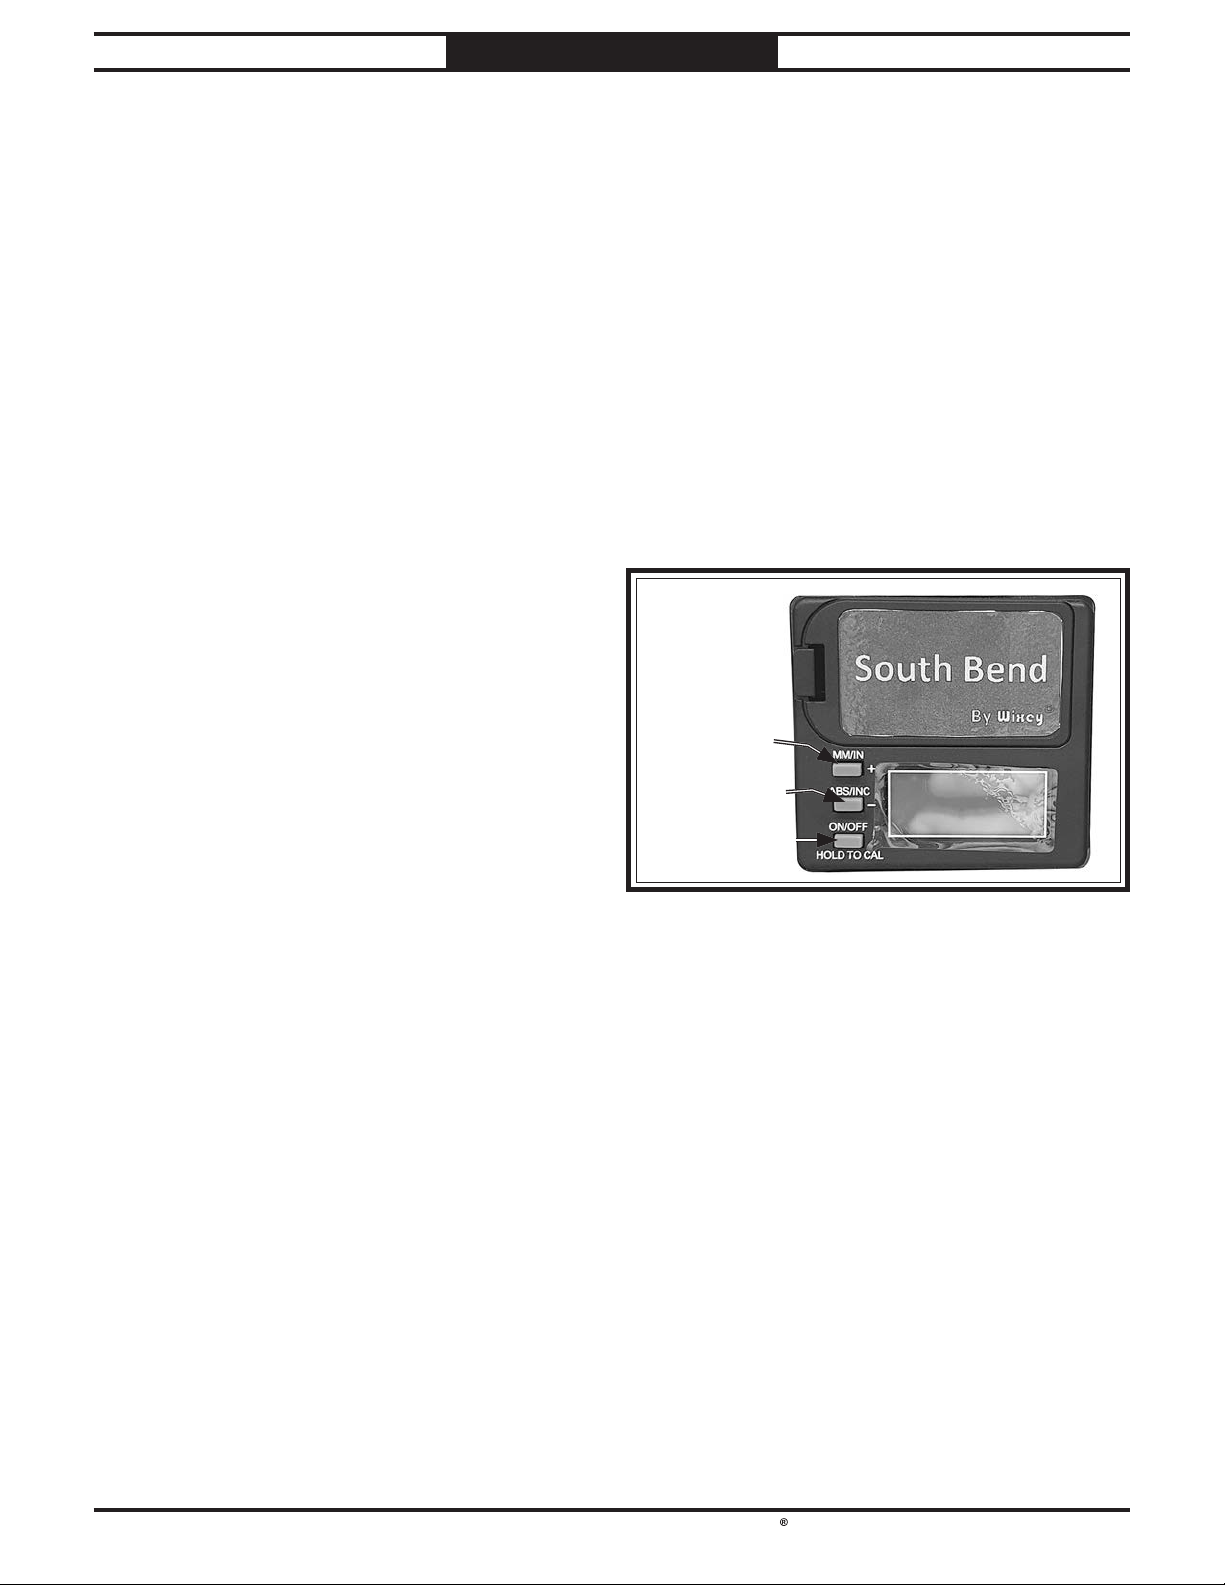
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
OPERATION
Digital Readout
The digital readout has two modes of use,
Absolute (ABS) and Incremental (INC).
When used in ABS mode, the readout displays
the distance between the table and the edge
of the cutterhead insert at bottom-dead-center
(BDC) to show workpiece thickness.
When INC mode is used, the readout displays the
distance between the current position of the table
and the position of the table where incremental
mode was set at 0 to show how much material
was removed from the workpiece.
To enter INC mode, press ABS/INC until INC is
displayed. Each time the unit is placed in INC
mode, the incremental value is reset to 0.
The digital readout is powered by 2 AAA
batteries. The readout will display a battery
icon when the battery level is low and needs
replacing. Each time the batteries are replaced,
the digital readout will need to be calibrated.
Calibrating Digital Readout
To calibrate digital readout:
1. Raise table all the way up.
Press mm/in button until 'in' is displayed.
2.
Press ABS/INC button until ABS is
3.
displayed. (This should already be displayed
by default after the batteries are replaced.)
Press and hold ON/OFF (CAL) button until
4.
ABS begins to flash (2–3 seconds).
Press + (mm/in) or – (ABS/INC) buttons to
5.
adjust readout until it displays 1⁄4".
Press ON/OFF button to return to normal
6.
operating mode.
-31-
Page 37
South Bend Tools
Model SB1108/ SB1109
order online at www.grizzly.com or call 1-800-523-4777
ACCESSORIES
For Machines Mfd. Since 12/20
Accessories
Accessories
This section includes the most common
accessories available for your machine through
our exclusive dealer, Grizzly Industrial, Inc., at
grizzly.com.
Installing unapproved accessories may
cause machine to malfunction, resulting in
serious personal injury or machine damage.
To reduce this risk, only install accessories
recommended by South Bend or Grizzly.
Refer to Grizzly’s website or latest catalog for
additional recommended accessories.
W1218A—Rotacator Precision Planer Tool
The Rotacator is a dial indicator on a magnetic
base, designed for quickly and accurately setting
the critical tolerances needed when making
planer adjustments. Perfect for adjusting infeed/
outfeed rollers, pressure bars, chip breakers,
and bed rollers. Also a great setup tool for other
machines! Accurate to 0.001". Indicator rotates
360°.
T28000—Bear Crawl (for SB1108)
T28923–Bear Crawl "Papa Bear" (for SB1109)
Heavy Duty Mobile Base
The Grizzly Bear Crawl Mobile Base, with a
1200 lb. capacity, steel and polyurethane heavyduty ball bearing wheels, and toe flip-stops,
will make this mobile base a staple under your
machines for years to come.
Adjusts from:
T28000–19" x 21" to 29
T28923–19" x 26" to 29
H9893—Indexable Carbide Inserts, 10-Pack
These indexable carbide inserts are designed
for use in spiral or helical cutterhead systems
and made to last up to 10 times longer than a
set of HSS steel straight blades. Made of solid
carbide. Size: 15 x 15 x 2.5mm.
1
⁄2" x 291⁄2"
1
⁄2" x 341⁄2"
-32-
Page 38
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
order online at www.grizzly.com or call 1-800-523-4777
ACCESSORIES
G5562—SLIPIT® 1 Qt. Gel
G5563—SLIPIT® 12 Oz. Spray
G2871—Boeshield® T-9 12 Oz. Spray
G2870—Boeshield® T-9 4 Oz. Spray
H3788—G96® Gun Treatment 12 Oz. Spray
H3789—G96® Gun Treatment 4.5 Oz. Spray
SB1365—South Bend Way Oil-ISO 68
Engineered for the high pressure exerted on
horizontal or vertical ways and slides. Protects
against rust and corrosion. Ensures stick-free,
smooth motion which maximizes finishes and
extends the life of your machine. Won’t gum up!
12 oz. AMGA#2 (ISO 68 Equivalent).
slipit
T28042—Moly-D Industrial Gear Oil-ISO 320
This industrial gear oil from Primrose has been
developed specifically for the high temperatures
and pressures typical of modern industrial
applications. 1-gallon size.
T26419—Syn-O-Gen NLGI #2 Synthetic Grease
100% pure synthesized hydrocarbon basestocks
compounded with special thickeners and
additives make Syn-O-Gen non-melt, tacky, and
water resistant. Extremely low pour point, high
temperature oxidation, and thermal stability
produce a grease unmatched in performance.
-33-
Page 39
South Bend Tools
Model SB1108/ SB1109
!
MAINTENANCE
MAINTENANCE
Maintenance Schedule
Always disconnect
machine from power before
performing maintenance or
serious personal injury may
result.
For optimum performance from your machine,
follow this maintenance schedule and refer to
any specific instructions given in this section.
Note: This maintenance schedule is based on
average daily usage. Adjust the maintenance
schedule to match your usage, to keep your planer
running smoothly, and to protect your investment.
Ongoing:
• Clean machine and protect unpainted cast
iron.
• Lubricate feed rollers bushings (Page 35).
• Tighten loose mounting bolts.
• Check/rotate/replace damaged or worn inserts
(Page 30).
• Check/repair/replace worn or damaged wires.
• Resolve any other unsafe condition.
Every 40 Hours of Operation:
• Clean cutterhead and inspect
inserts (Page 30).
• Lubricate table columns and leadscrews
(Page 35).
• Inspect/Clean anti-kickback fingers
(Page 37).
Every 160 Hours of Operation:
• Check/tension/replace V-belts (Page 38).
• Clean/vacuum dust buildup from inside
cabinet and off motor.
• Lubricate table height worm gear (Page 36).
• Lubricate table height chain and sprockets
(Page 36).
• Lubricate drive chain and sprockets
(Page 36).
For Machines Mfd. Since 12/20
Cleaning & Protecting
Vacuum excess wood chips and sawdust, and wipe
off the remaining dust with a dry cloth. If any
resin has built up, use a resin-dissolving cleaner
to remove it.
Protect the unpainted cast-iron table by wiping
it clean after every use—this ensures moisture
from wood dust does not remain on bare
metal surfaces. Keep the table rust-free with
regular applications of products like G96
Treatment, SLIPIT
33 for more details).
®
, or Boeshield® T-9 (see Page
®
Gun
Machine Storage
All machinery will develop serious rust problems
and corrosion damage if it is not properly
prepared for storage. If decommissioning this
machine, use the steps in this section to ensure
that it remains in good condition.
To prepare machine for storage or
decommission from service:
1. Disconnect all power sources to the machine.
2. Thoroughly clean all unpainted, bare metal
surfaces, then coat them with a light weight
grease or rust preventative. Take care to
ensure these surfaces are completely covered
but that the grease or rust preventative is
kept off of painted surfaces.
Note: If the machine will be out of service for
only a short period of time, use way oil or a
good grade of medium-weight machine oil
(not auto engine oil) in place of the grease or
rust preventative.
Loosen or remove belts so they do not become
3.
stretched while the machine is not in use.
Yearly:
• Change gearbox oil (Page 37).
-34-
Page 40
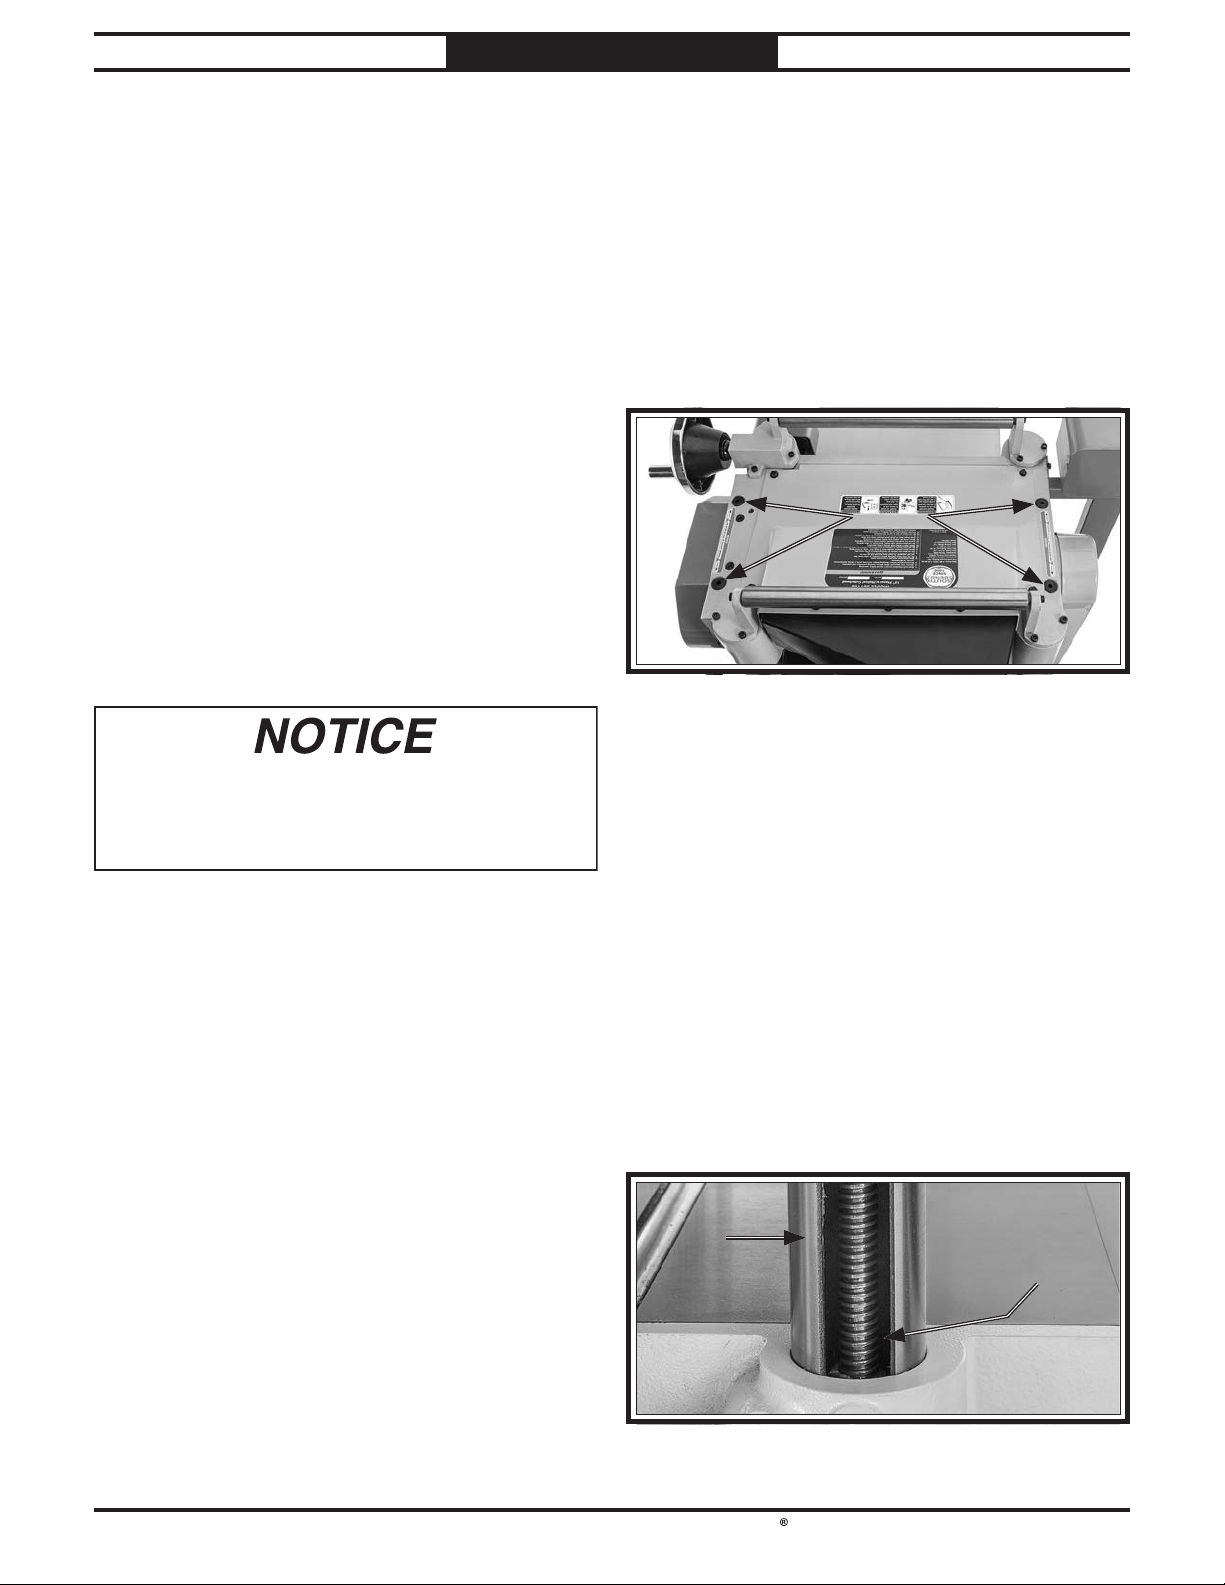
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
MAINTENANCE
4. Fill the gearbox with the recommended gear
oil so components above the normal oil level
do not develop rust. (Make sure to put a tag
on the controls as a reminder for the recommissioning process to adjust the gear oil
level before starting the machine.)
Note: If the machine will be out of service
for only a short period of time, start the
machine once a week and run all gear-driven
components for a few minutes. This will
put a fresh coat of gear oil on the gearing
components inside the gearbox.
Completely cover the machine with a tarp
5.
or plastic sheet that will keep out dust and
resist liquid or moisture. If machine will be
stored in/near direct sunlight, use a cover
that will block the sun's rays.
Lubrication
Feed Roller Bushings
Oil Type ..................SB1365 or ISO 68 Equivalent
Oil Amount
Frequency
The infeed and outfeed rollers rotate inside
bushing blocks on both ends of the rollers. Add
2–3 drops of ISO 68 machine oil to the center
hole of the four feed roller tension adjustment
bolts on top of the head casting, as shown in
Figure 39.
............................................. 2–3 Drops
.................. Every 8 Hours of Operation
Lubricate feed roller bushings
Failure to follow reasonable lubrication
practices as instructed in this manual for your
machine could lead to premature failure of
components and void the warranty.
Your planer features bearings that are lubricated
and sealed at the factory. These bearings do not
require any further attention unless they need
to be replaced. If a bearing fails, your planer
will probably develop a noticeable rumble or
vibration, which will increase when the machine
is under a load. The bearings are standard sizes
and can be replaced through Grizzly.
Follow the maintenance schedule on this page
and the procedures beginning on Page 33 to
properly lubricate the other planer components,
which are essential for long life and trouble-free
operation of your planer.
Columns & Leadscrews
Oil Type ..................SB1365 or ISO 68 Equivalent
Oil Amount
Grease Type
Frequency
The table rides on the columns and is moved by
the rotation of the leadscrews inside the columns.
Loosen the dust sleeve to access the columns and
leadscrews (see Figure 40). Apply a thin coat
of ISO 68 machine oil to the outside surface of
the columns and brush on a light application of
multi-purpose grease to the leadscrew threads.
Move the table up and down to distribute the
lubricant.
............................................. Thin Coat
............................NLGI#2 Equivalent
................ Every 40 Hours of Operation
Lubricate column and leadscrews
-35-
Page 41
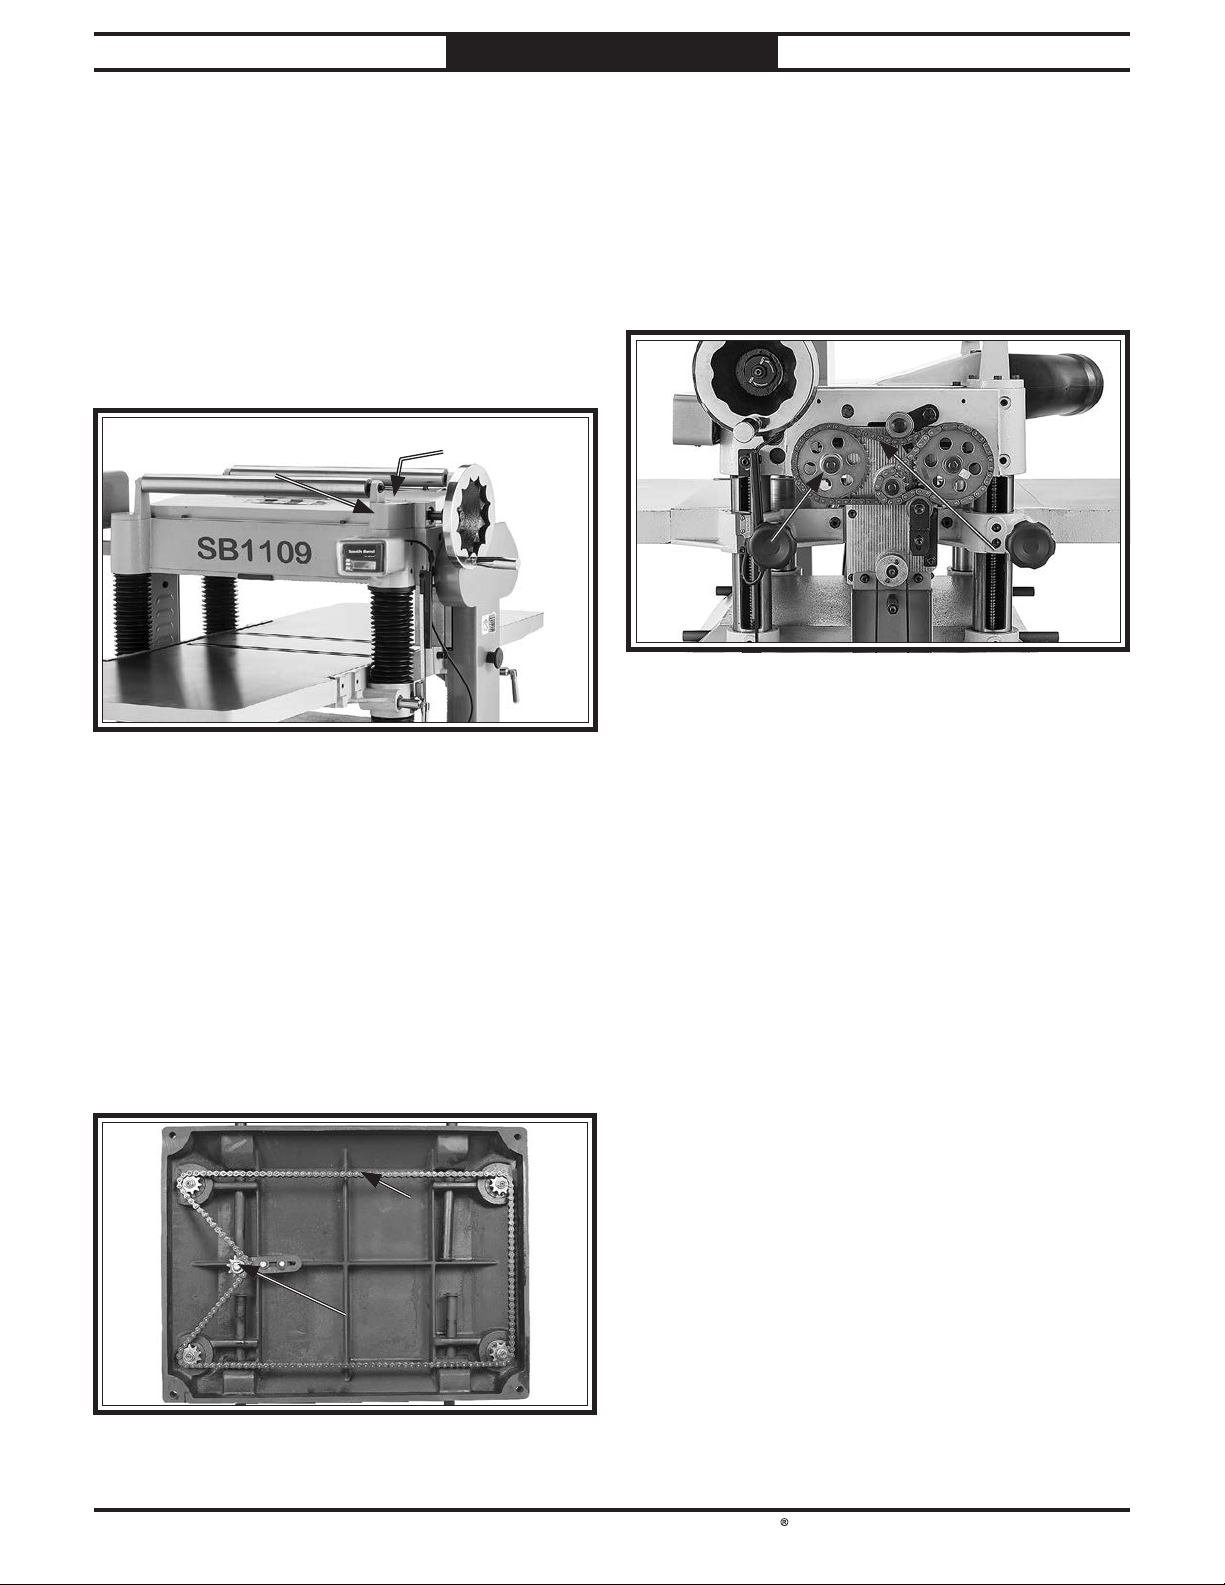
South Bend Tools
Model SB1108/ SB1109
MAINTENANCE
For Machines Mfd. Since 12/20
Table Height Worm Gear
Grease Type .......... T26419 or NLGI#2 Equivalent
Frequency
Remove the three cap screws that secure the
worm gear housing (see Figure 41), then lift
the housing and handwheel assembly off the
machine. Clean away any debris from the
housing and gears, then brush on a moderate
amount of multi-purpose grease to the gear
teeth.
.............. Every 160 Hours of Operation
Lubricate table ht worm gear
Drive Chain & Sprockets
Grease Type .......... T26419 or NLGI#2 Equivalent
Frequency
The infeed and outfeed rollers receive the
transferred power from the cutterhead through
the drive chain system on the right side of the
machine, as shown in Figure 43.
.............. Every 160 Hours of Operation
Drive chain and sprockets
Table Height Chain & Sprockets
Lubricate chain and sprockets
Grease Type .......... T26419 or NLGI#2 Equivalent
Frequency
The table leadscrews are synchronized by
the table height chain and sprockets located
underneath the planer base (see Figure 42).
Use shop rags and mineral spirits to clean
away debris and grime, then brush a light coat
of multi-purpose grease onto the chain and
sprockets.
.............. Every 160 Hours of Operation
Use shop rags and mineral spirits to clean away
any debris and grime, then brush a light coat
of multi-purpose grease onto the chain and
sprockets.
-36-
Page 42
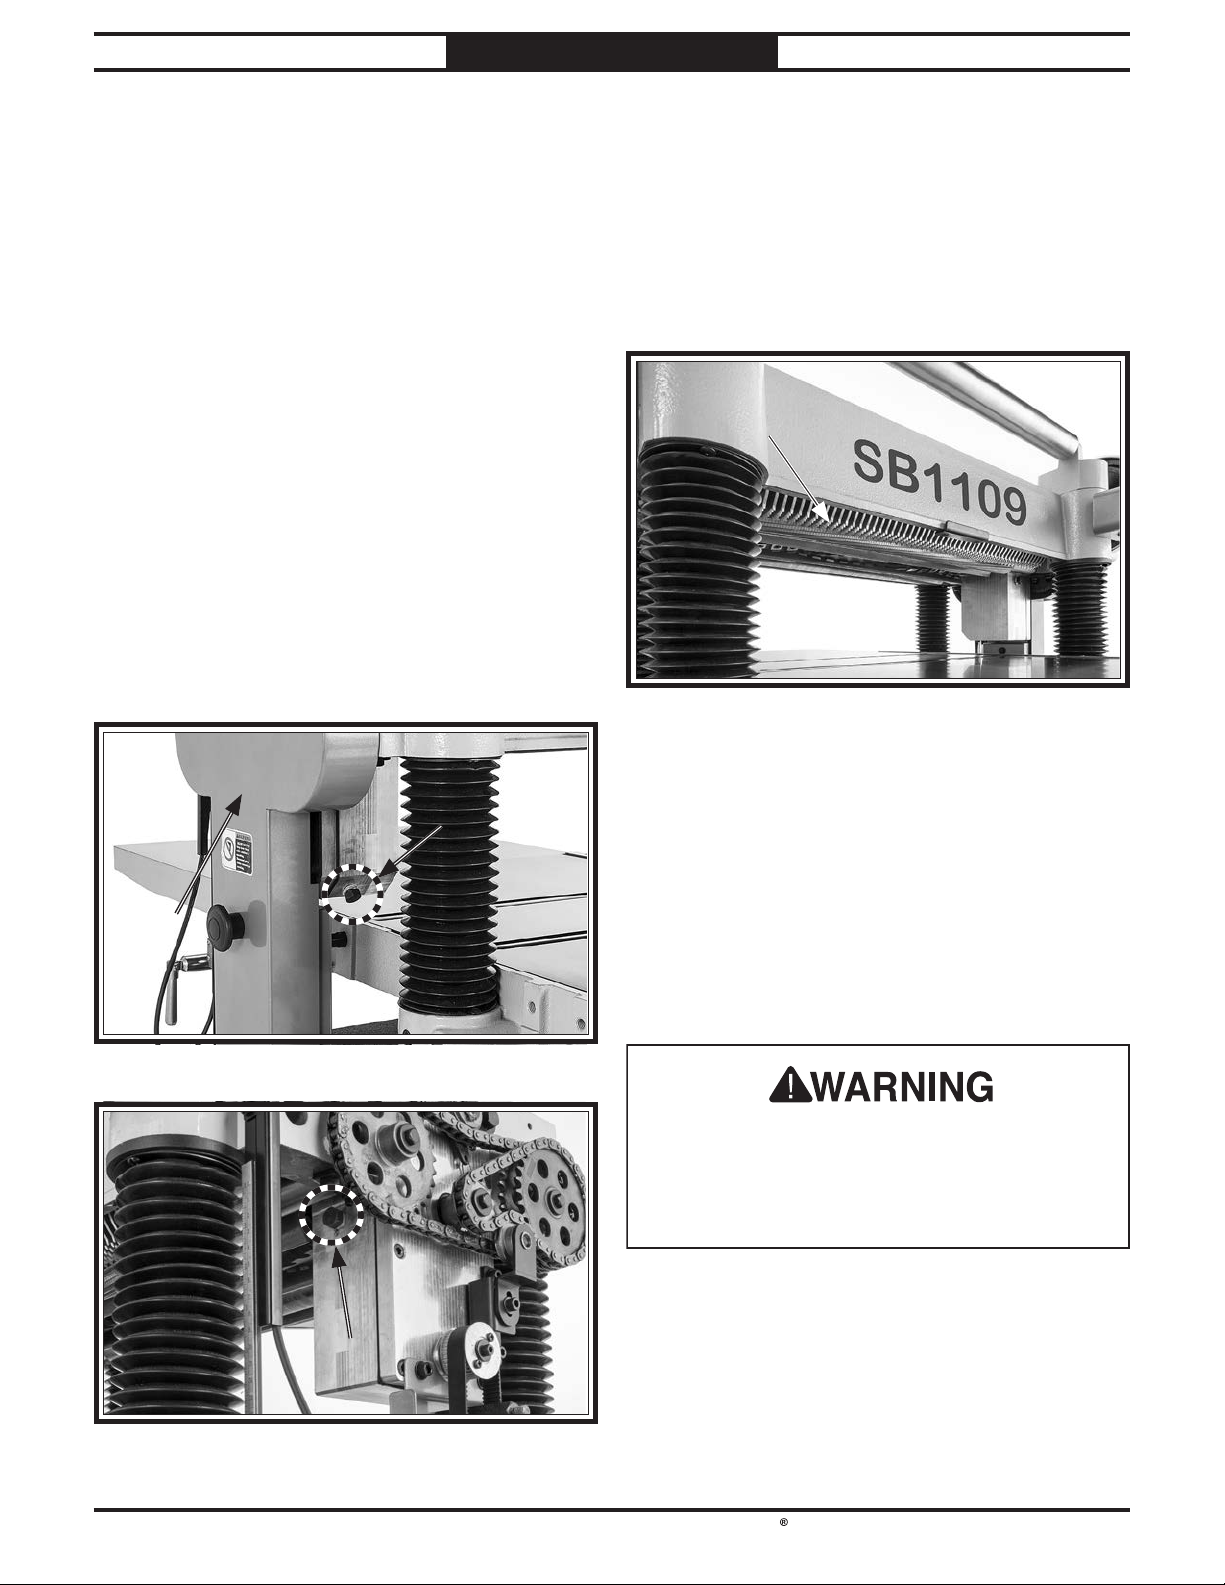
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
Check the anti-kickback fi ngers regularly to
ensure they swing freely and easily. If the fi ngers
do not swing freely and easily, fi rst clean them
with a wood-resin solvent, then inspect them
for damage. If any of the fi ngers are damaged,
the device must be replaced before using the
machine.
Do not apply oil or other lubricants to the antikickback fi ngers that will attract dust and
restrict free movement of the fi ngers.
MAINTENANCE
Gearbox Oil
Oil Type ................ T28042 or ISO 320 Equivalent
Oil Amount
Frequency
Note: SAE 140 Gear Oil or SAE 85W-140 multiweight gear oil may also be used. DO NOT mix
oil types!
Note: We recommend that you replace the
gearbox oil after the first 20 hours of operation.
This is a normal break-in procedure and will
help maximize the service life of the machine by
flushing away any particles from the break-in
process.
Although it is not necessary to remove the drive
chain cover to access the fill and drain plugs, it
is more convenient to do so (see Figures 44–45).
Drain the old oil into a pan. Re-install the drain
plug, then refill the gearbox with ISO 320 or
equivalent oil until it just reaches the fill plug.
Re-install the fill plug.
................................................... 20 Oz.
....... After First 20 Hours, Then Yearly
Anti-Kickback Fingers
The anti-kickback fingers are an important
safety feature of your planer. The fingers hang
from a rod suspended across the head casting
and in front of the infeed roller, as shown. This
design allows the workpiece to easily enter
the planer but reduces the risk of kickback by
digging into the workpiece if it moves backward.
Anti Kickback Fingers
Proper operation of anti-kickback fi ngers is
critical for safe operation of this planer. DO
NOT operate planer if anti-kickback fi ngers are
not operating correctly. Failure to heed this
warning could result in serious personal injury.
-37-
Page 43
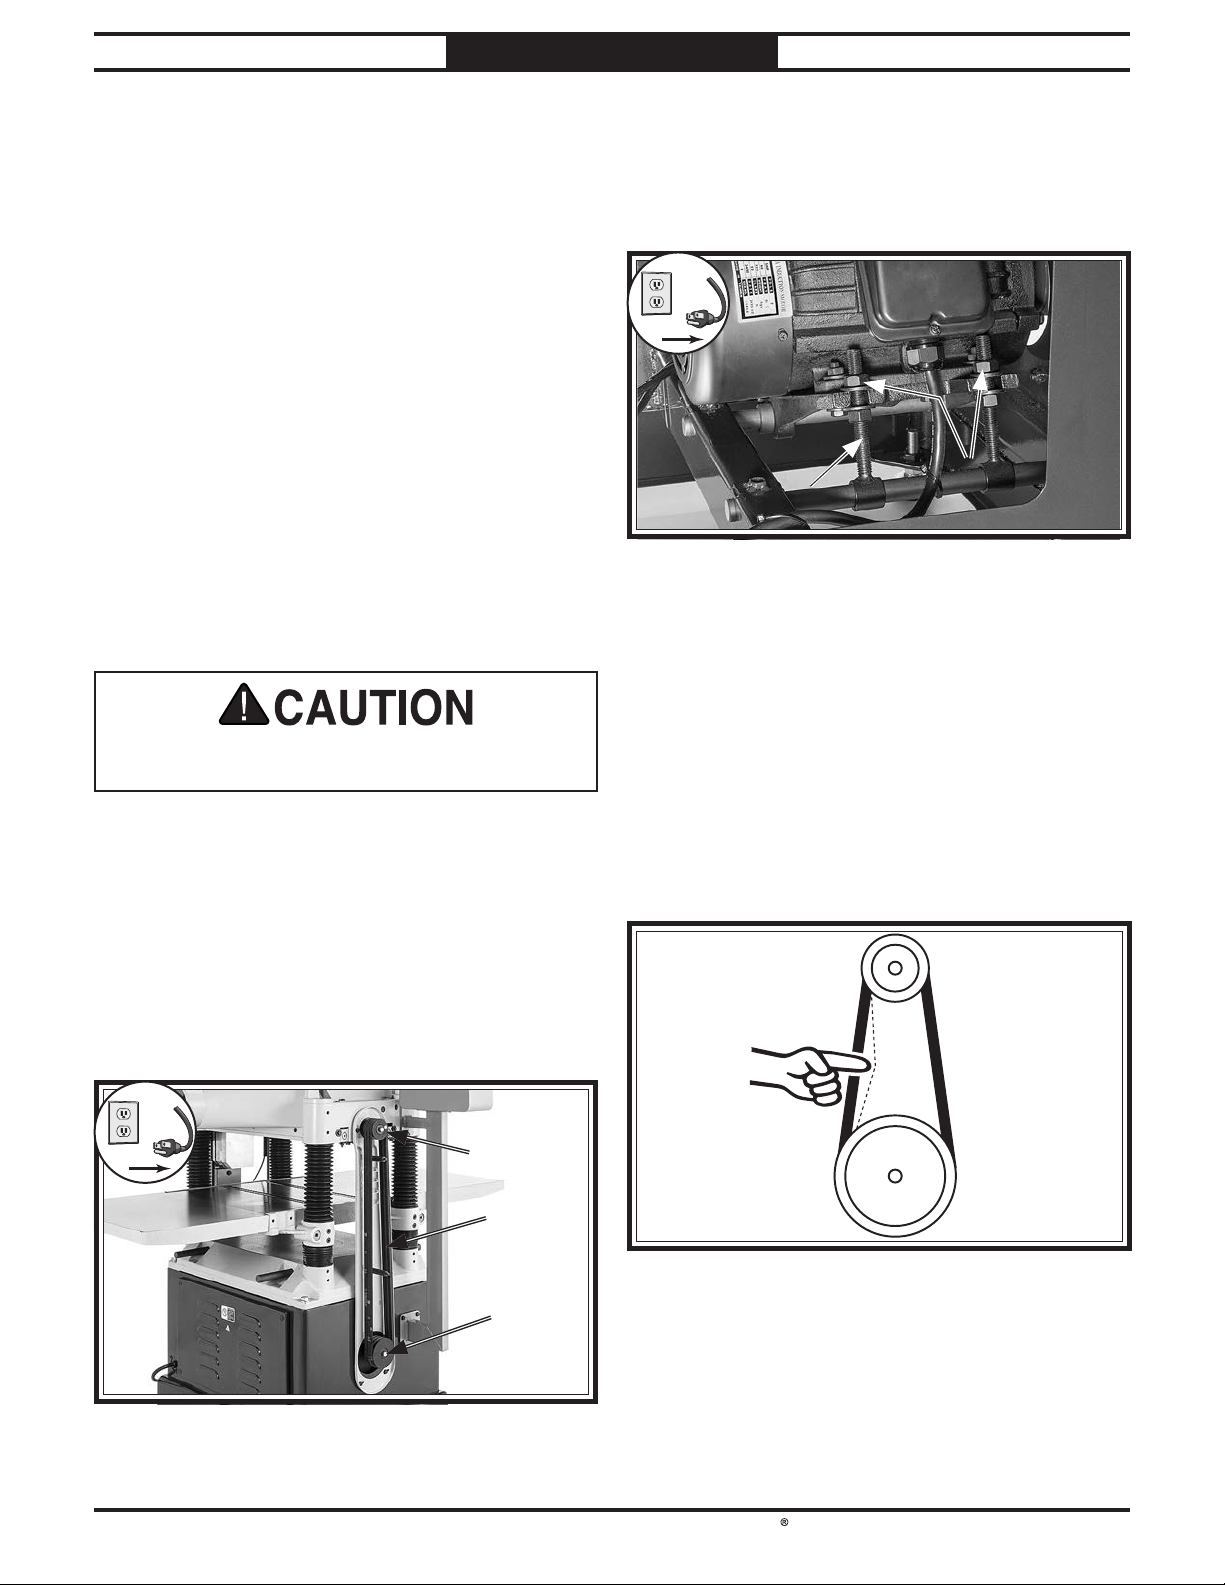
South Bend Tools
Model SB1108/ SB1109
!
!
SERVICE
For Machines Mfd. Since 12/20
Tensioning/Replacing V-Belts
Three V-belts transfer power from the motor
to the cutterhead, and then to the infeed and
outfeed rollers with the use of the drive chain
system. To ensure efficient transfer of power to
these systems, make sure the V-belts are always
properly tensioned and in good condition.
If the V-belts are worn, cracked, or damaged,
replace them. Always replace all V-belts at the
same time with a matched set of three, or belt
tension may not be even among the belts, causing
premature belt failure or weakened power
transfer.
Items Needed Qty
Phillips Screwdriver #2 ........................................1
Open-End Wrench 19mm
.....................................1
3. Remove rear cabinet cover to access motor
mount hex nuts (see Figure 48).
Note: SB1108 has (1) motor mount
connecting rod, SB1109 has (2).
4.
If V-belts need to be replaced, raise motor
to release belt tension, roll them off pulleys,
then replace with a matched set of three.
V-belts and pulleys will be hot after operation.
Allow them to cool before handling.
To tension/replace V-belts:
1.
DISCONNECT MACHINE FROM POWER!
2. Remove V-belt cover from left side of
machine to expose belts (see Figure 47).
Note: A collection of black belt dust at the
bottom of the belt cover is normal during the
life of the belts.
To adjust V- belt tension, loosen top motor
5.
mount hex nuts (see Figure 48), then adjust
bottom hex nuts to raise or lower motor.
Note: V-belts are properly tensioned when
there is approximately
moderate pressure is applied to them midway
between pulleys, as illustrated in Figure 49.
Approximately
3
⁄4" Deflection
3
⁄4" deflection when
Disc
Pulley
Motor
Pulley
-38-
6. After V-belts are properly tensioned, tighten
top motor mount hex nuts, then re-install
cabinet cover and belt cover.
Page 44
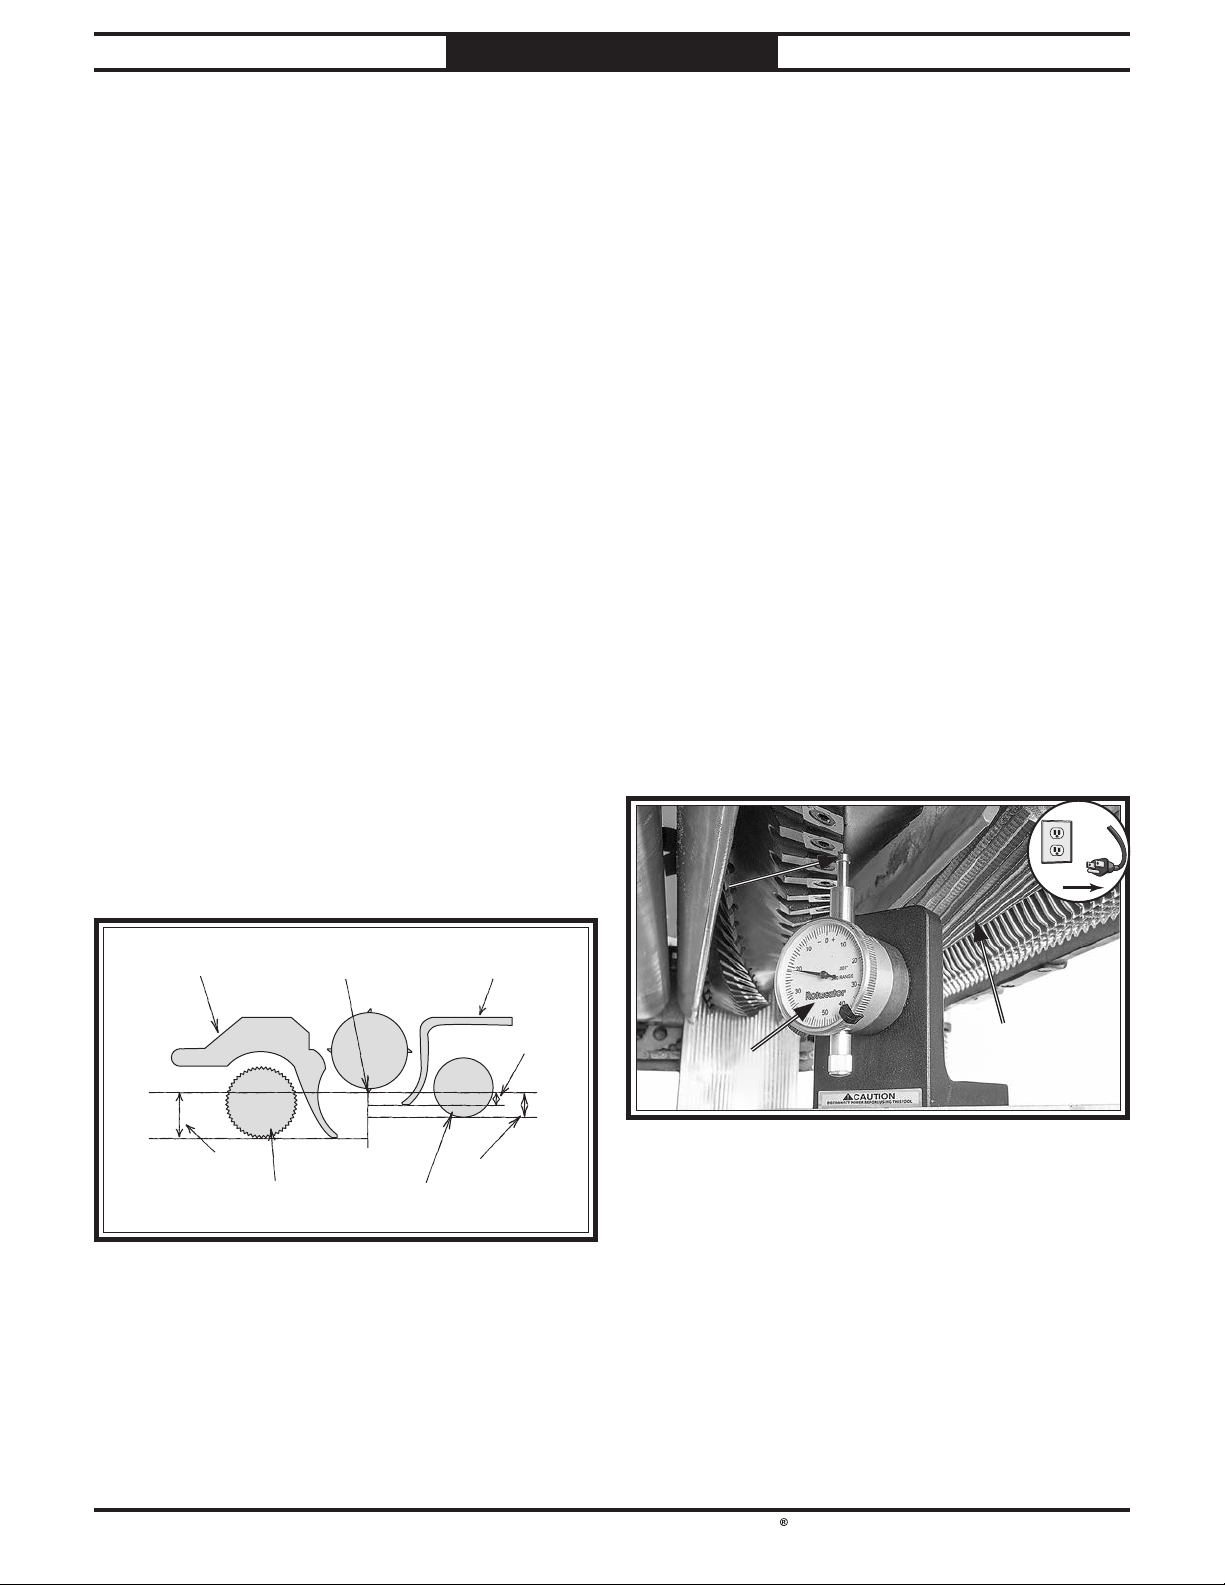
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
!
SERVICE
Setting Feed Roller,
Setting Feed Roller, Chip Breaker
Chip Breaker &
& Pressure Bar Heights
Pressure Bar Heights
It is essential that the feed rollers, chip
breaker, and pressure bar are set at the correct
distance below the cutterhead knives/inserts
at BDC (bottom dead center) to ensure that the
workpiece moves through the planer evenly and
the correct distance from the cutterhead knives/
inserts.
To ensure accurate results and make the
adjustment process quicker and easier, we
recommend using a Rotacator for these
adjustments (refer to Page 32).
If a Rotacator is not available, a 6' 2x4 cut into
two even-sized pieces and a feeler gauge set can
be used, but care must be taken when jointing
the wood to achieve accurate results and ensure
both boards have the exact same height.
Dist. Below Cutterhead Insert at BDC (Figure 50)
Infeed Roller ...........................................0.040"
A.
Chip Breaker ..........................................0.040"
B.
Pressure Bar ...........................................0.008"
C.
Outfeed Roller ........................................0.020"
D.
Using a Rotacator
Items Needed Qty
Hex Wrenches 3mm, 5mm ............................. 1 Ea.
Wrench or Socket 10mm
Rotacator (see Page 32)
To use a Rotacator to check/adjust heights:
1. DISCONNECT MACHINE FROM POWER!
2. Make sure all inserts are properly installed
(refer to Rotating/Replacing Cutterhead
Inserts on Page 30 for detailed
instructions).
Lower table at least 4" below head casting,
3.
then lock it in place.
Remove dust hood, top cover, belt cover, and
4.
drive chain cover.
Using your Rotacator, find bottom dead
5.
center (BDC) of any insert edge by
slowly rocking cutterhead pulley back
and forth, then set Rotacator dial to "0"
(see Figure 51).
................................ 1 Ea.
.......................................1
Chip
Breaker
A & B
(Bottom Dead Center)
Infeed
Roller
BDC
Outfeed
Roller
Pressure
Bar
D
C
Move feed rate control knob to neutral
6.
position to allow infeed roller to freely rotate.
-39-
Page 45
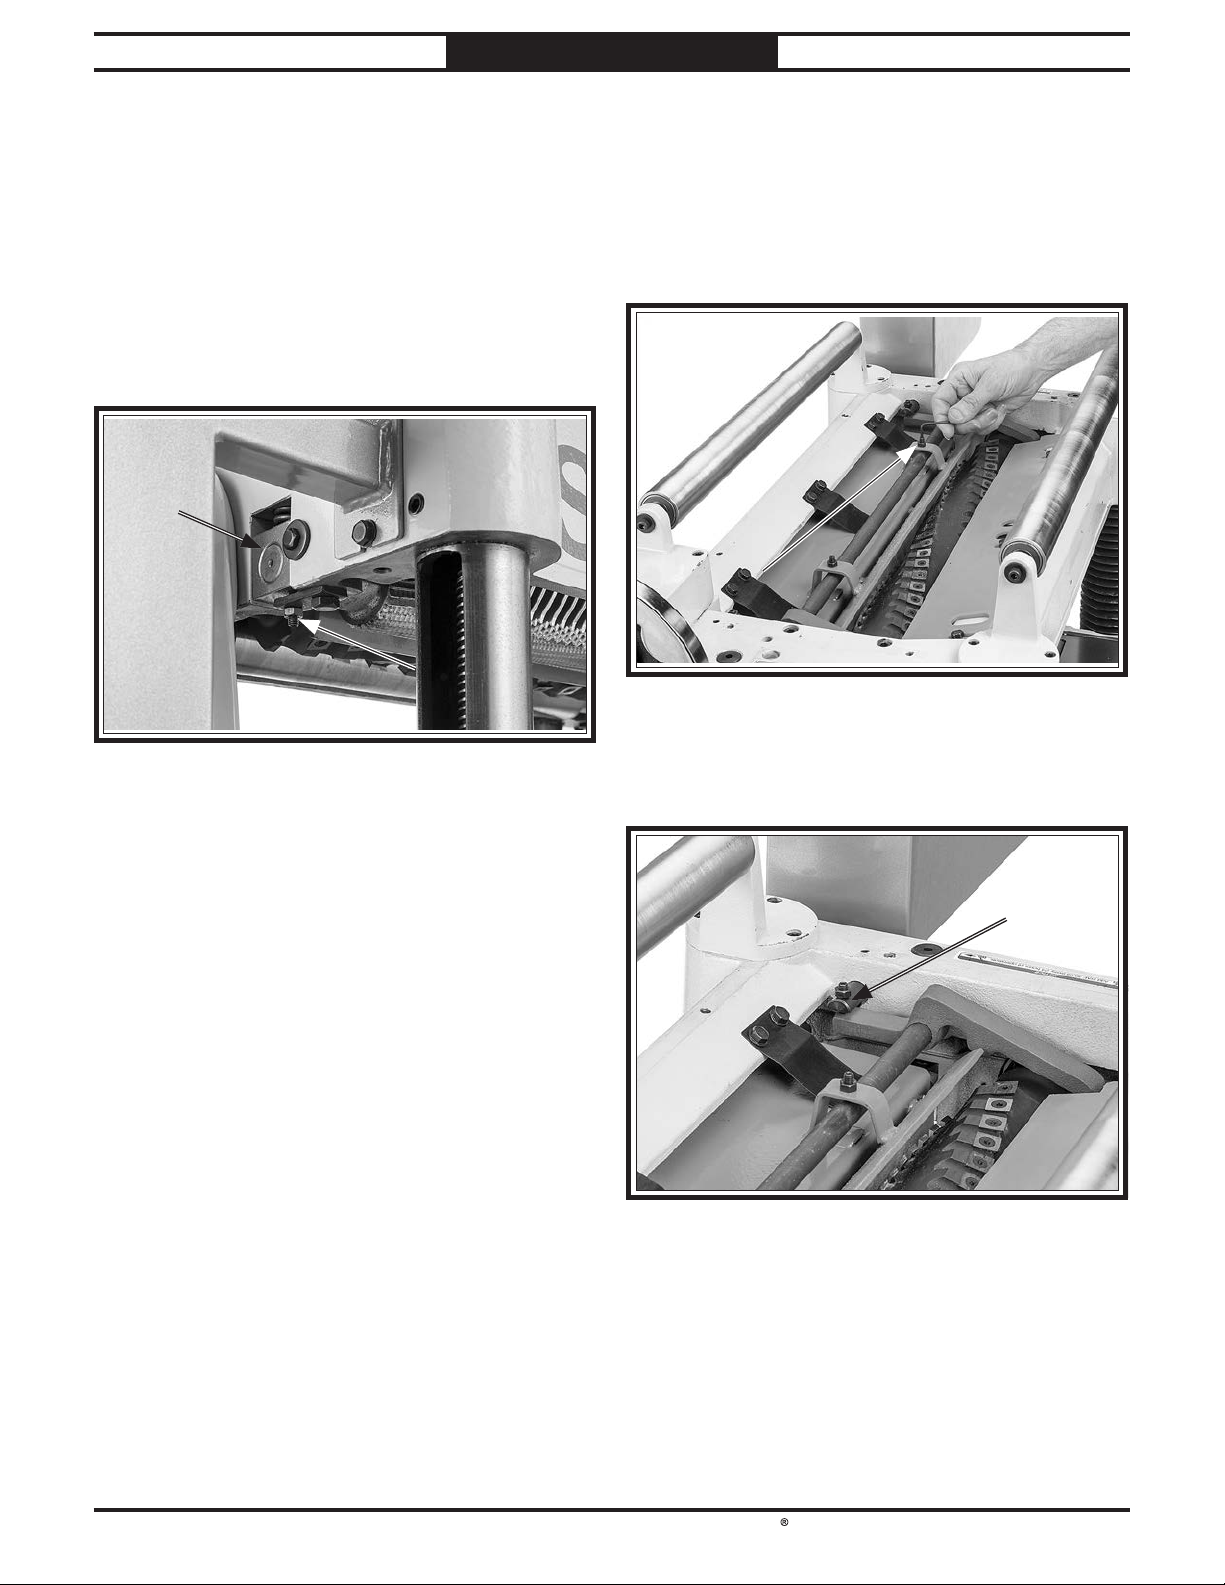
South Bend Tools
Model SB1108/ SB1109
SERVICE
For Machines Mfd. Since 12/20
Keeping Rotacator dial at "0", position it
7.
under right-hand side of infeed roller and
find BDC of a serrated edge by rocking
infeed roller back and forth.
8. Loosen jam nuts and use set screws on each
side of feed roller as shown to adjust height
of infeed roller bushing block until Rotacator
dial shows 0.040", which is the recommended
distance for infeed roller below the
cutterhead (see Figure 52).
Using same "0" reference on Rotacator
12.
dial from Step 5, perform similar steps as
described previously to adjust height of chip
breaker to its recommended specification
given at beginning of this subsection.
The adjustment controls are shown below
(see Figure 53).
Repeat Steps 7–8 on left side of feed roller.
9.
Re-check both sides of infeed roller and, if
10.
necessary, make further adjustments until
infeed roller height from side to side is
0.040" below BDC of cutterhead insert, then
retighten both jam nuts.
Keeping same "0" reference on Rotacator dial
11.
from Step 5, repeat Steps 7–10 for outfeed
roller, but adjust it until it is 0.020" below
BDC of cutterhead insert.
Repeat Step 12 for pressure bar height
13.
adjustment using adjustment controls shown
in Figure 54.
Re-install belt cover, top cover, chain cover,
14.
and dust hood.
-40-
Page 46
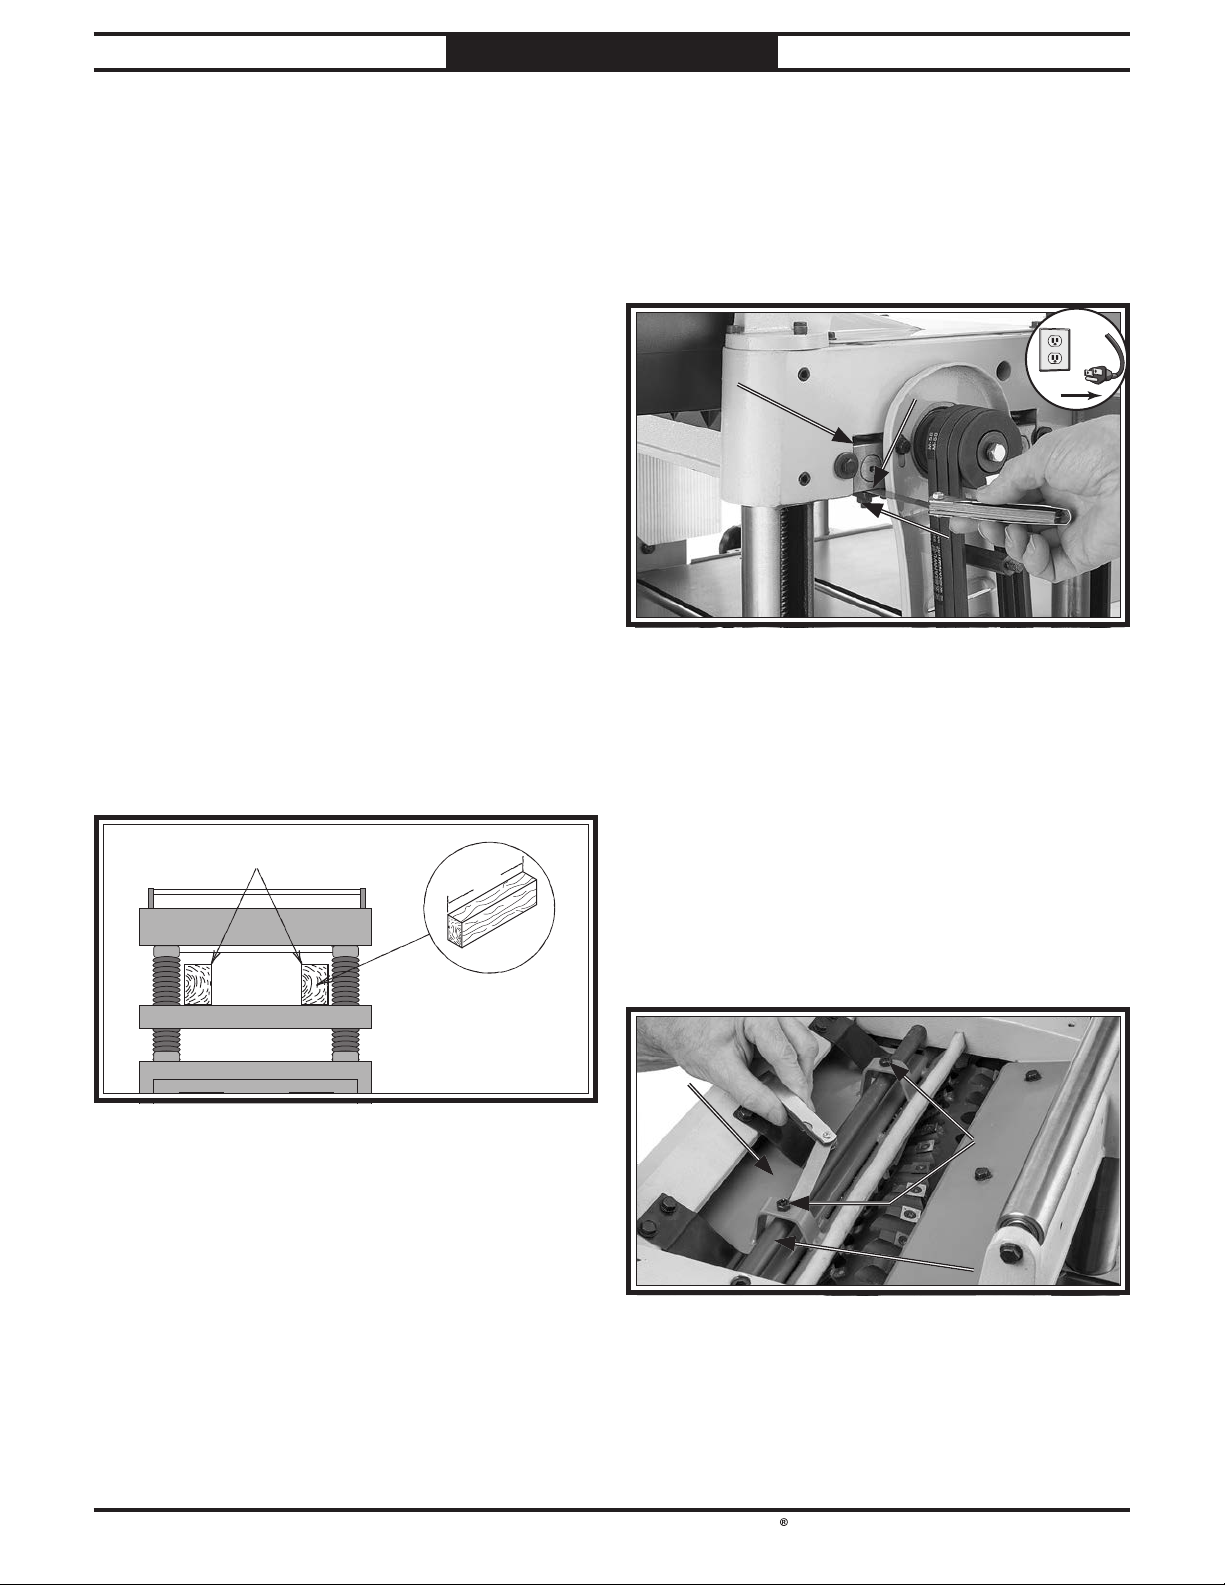
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
!
SERVICE
Using Wood Blocks
Items Needed Qty
Hex Wrench 3mm, 5mm ....................................... 1
Wrench or Socket 10mm
2x4 6' Long
Feeler Gauge Set
.............................................................1
................................................... 1
To use wood blocks to check/adjust heights:
1. Build wood blocks by cutting a straight
6-foot-long 2x4 in half.
Note: Having the wood blocks at an even
height is critical to the accuracy of your
overall adjustments. For best results, make
the 2x4 square with a jointer and table saw
before cutting it in half.
DISCONNECT MACHINE FROM POWER!
2.
3. Lower bed rollers below table surface (refer
to Bed Roller Height on Page 29 for
detailed instructions).
....................................... 1
7. Loosen jam nuts and set screws on each side
of infeed roller (see Figure 56).
Using feeler gauge, adjust set screw so it
8.
is 0.040" from roller bushing block (see
Figure 56), then tighten jam nut. Repeat on
other side of infeed roller.
Place wood blocks along sides of table, as
4.
illustrated in Figure 55, then raise table
until blocks are close to cutterhead.
Wood Blocks
36"
5.
Remove dust hood, top cover, belt cover, and
drive chain cover.
Using belt to rotate cutterhead, continue
6.
to raise table until blocks just barely touch
cutterhead insert at its lowest point of
rotation (BDC), then lock table in place.
Repeat Steps 8–9 with outfeed roller, only
9.
adjust the gaps to 0.020".
Loosen jam nuts and set screws on each side
10.
of chip breaker (see Figure 57).
Using a feeler gauge, adjust set screw so
11.
chip breaker is 0.040" from cross bar (see
Figure 57), then tighten jam nut. Repeat on
other side of chip breaker.
Note: The wood blocks will hold infeed and
outfeed rollers, chip breaker, and pressure
bar at same level as insert at BDC.
Re-install belt cover, top cover, drive chain
12.
cover, and dust hood.
-41-
Page 47
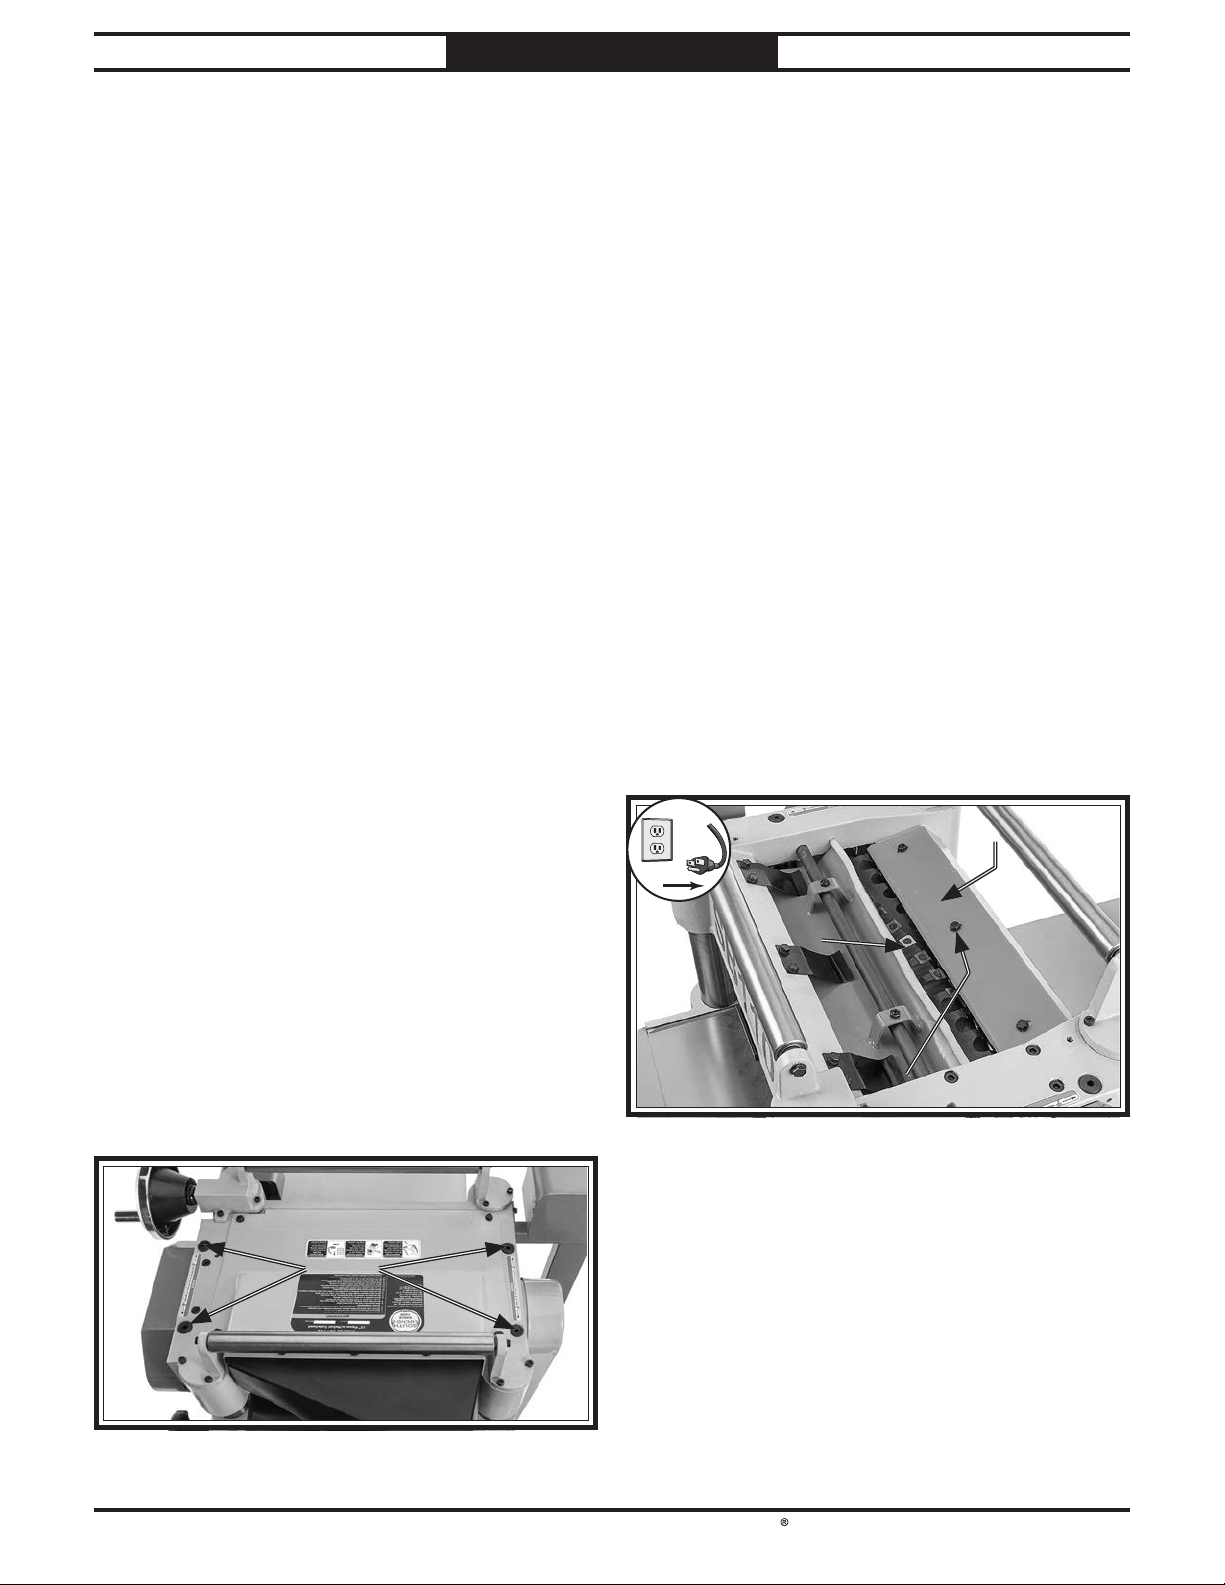
South Bend Tools
Model SB1108/ SB1109
When properly distanced from the cutterhead,
the chip defl ector directs the chips into the
dust hood, and keeps them from falling onto
the outfeed roller and being pressed into the
workpiece.
!
SERVICE
For Machines Mfd. Since 12/20
Adjusting Feed-Roller Spring Tension
The infeed and outfeed rollers keep the
workpiece moving through the planer. Springs
exert downward pressure on the feed rollers
while allowing them to raise with an uneven
workpiece surface. Proper spring tension is
crucial to keep the workpiece moving through the
planer during operation without pulling from one
side to the other.
The ideal feed-roller spring tension varies
depending upon the type of wood you plane.
When adjusting spring tension, keep the
following in mind:
• If you are planing milled lumber with a
consistent surface, use less spring tension to
reduce the risk of marring the workpiece.
• If you are planing rough lumber with
inconsistent surfaces, use greater spring
tension to keep the stock moving through the
planer.
Positioning Chip
Deflector
Chip Deflector Gap Setting
Tools Needed Qty
Wrench or Socket 10mm ....................................... 1
Hex Wrench 5mm
To adjust chip deflector gap:
DISCONNECT MACHINE FROM POWER!
1.
2. Remove dust hood, top cover, and belt cover.
3. Use cutterhead pulley to rotate cutterhead
until an insert reaches closest distance to
chip deflector (see Figure 59), then measure
distance between insert and chip deflector.
.................................................1
........................1⁄16"– 1⁄4"
• If the workpiece consistently stops feeding
during operation, the spring tension may
need to be increased.
Items Needed Qty
Hex Wrench 5mm .................................................1
To adjust feed-roller spring tension:
DISCONNECT MACHINE FROM POWER!
1.
2. Rotate tension screws clockwise to increase
tension or counterclockwise to decrease
tension (see Figure 58).
4. If distance measured in Step 3 is not equal
to correct chip deflector gap setting, then
loosen (3) flange bolts that secure chip
deflector and adjust gap to correct setting.
Re-tighten flange bolts, then replace belt
5.
cover, top cover, and dust hood.
-42-
Page 48
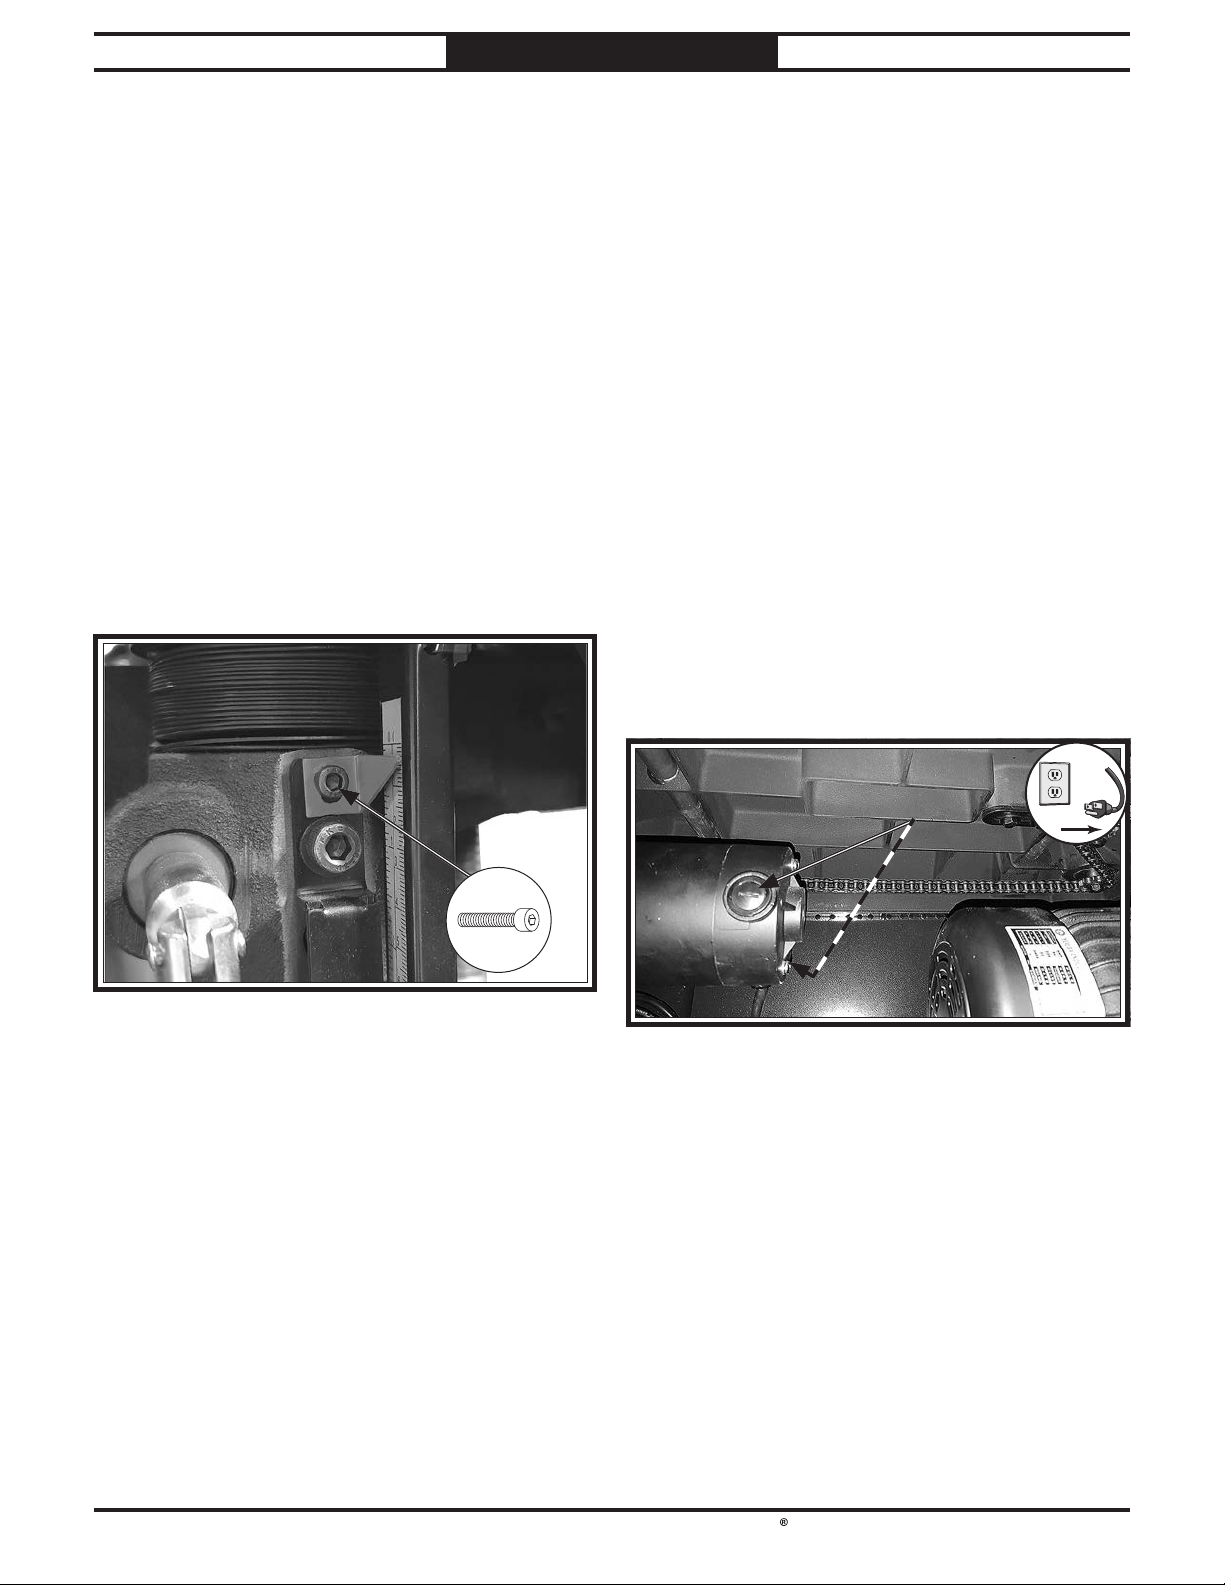
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
!
SERVICE
Calibrating Table Height Scale
Although correctly set at the factory, the table
height scale can be adjusted for accuracy if it
becomes necessary.
Items Needed Qty
Hex Wrench 4mm .................................................1
To calibrate table height scale:
1. Raise table all the way up.
2. Loosen scale pointer cap screw shown in
Figure 60.
Adjust scale pointer to 1⁄4" mark on scale,
3.
then tighten cap screw (see Figure 60).
Replacing Feed Motor Brushes
The models SB1108 and SB1109 feature a DC
motor that is used to control the feed rollers,
which uses heavy-duty carbon brushes. While
these brushes are design for extended life, they
will eventually wear out, causing loss of power or
faulty starting..
Items Needed Qty
Phillips Screwdriver #2 ........................................1
Flat Head Screwdriver
Motor Brushes
To replace feed motor brushes:
1. DISCONNECT MACHINE FROM POWER!
2. Remove motor access panel.
3. Remove DC motor brush cover, then pull out
used motor brush (see Figure 61).
................................................ 1 Set
..........................................1
Figure 60. Location of adjustment screw for table
height scale.
x1
4.
Insert new motor brush, then re-install and
tighten brush cover.
Repeat Step 4 to replace second motor
5.
brush.
Re-install motor access cover.
6.
-43-
Page 49
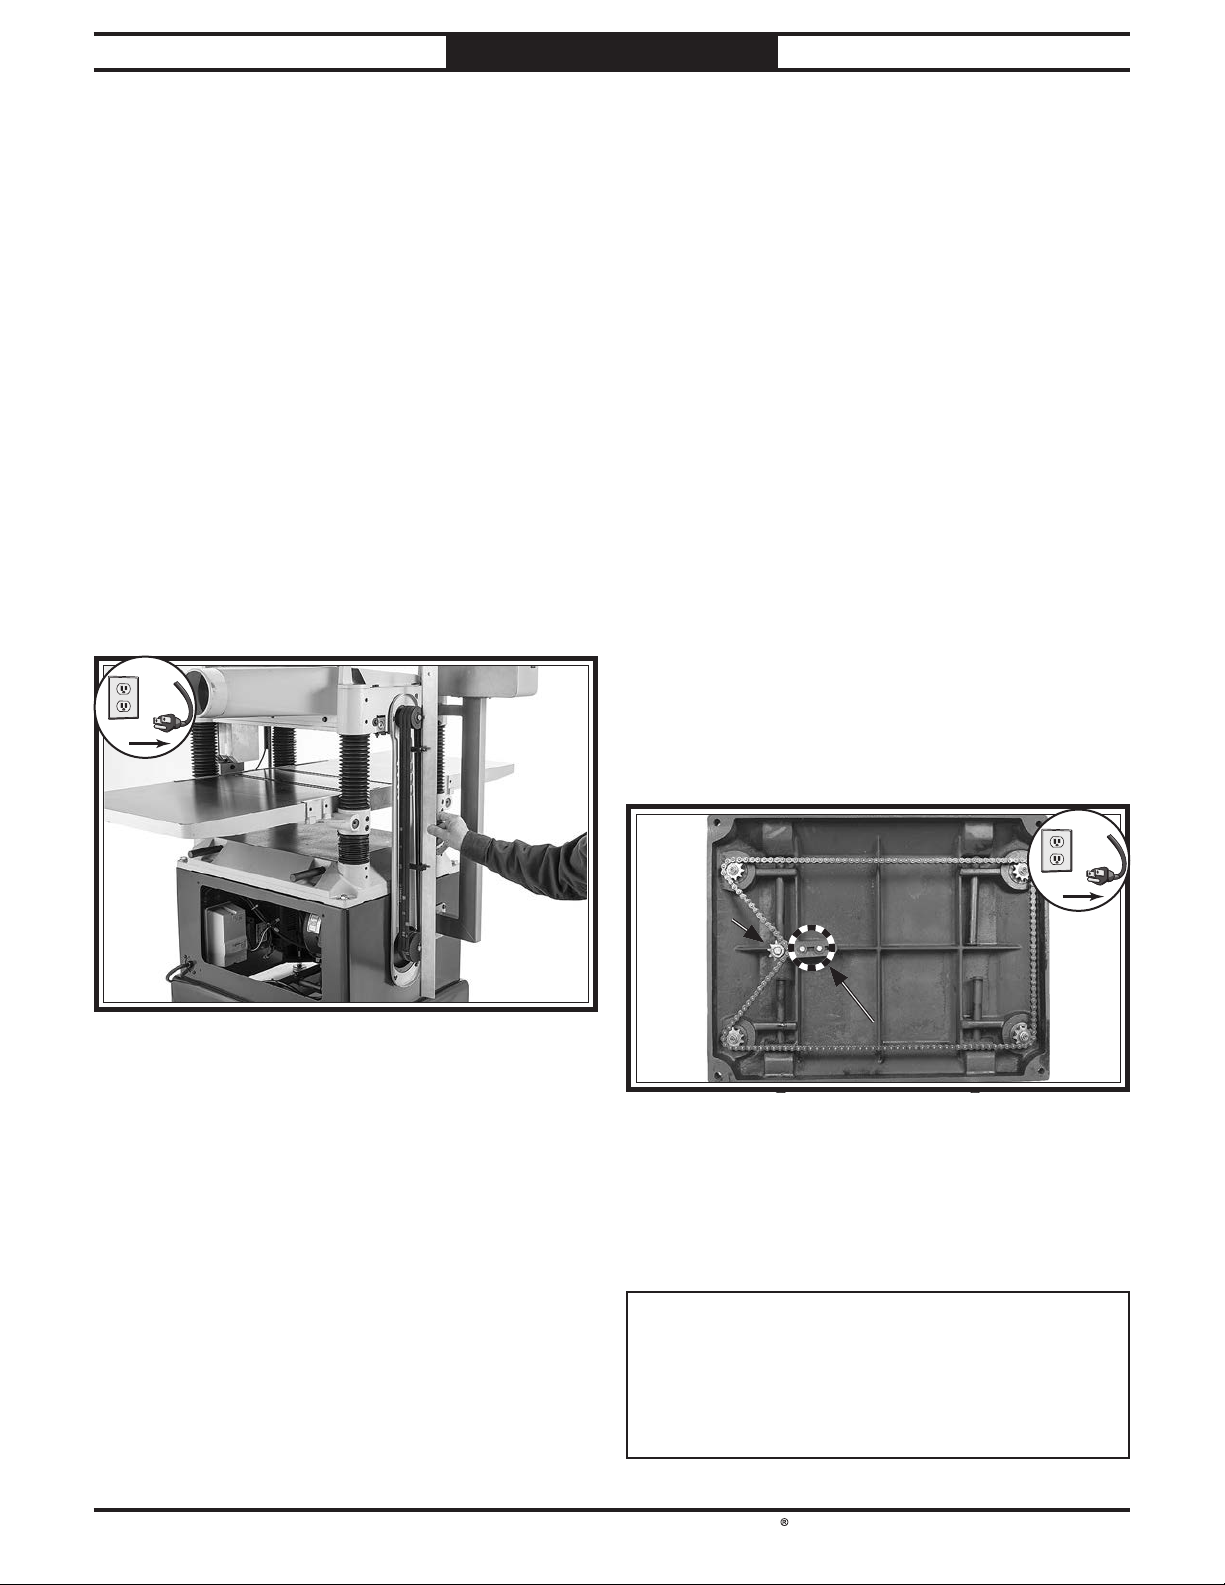
South Bend Tools
Model SB1108/ SB1109
!
!
SERVICE
For Machines Mfd. Since 12/20
Checking Pulley Alignment
Proper pulley alignment prevents premature
V-belt wear and proper power transfer from the
motor. The pulleys are properly aligned when
they are parallel and in the same plane as each
other.
Items Needed Qty
Straightedge 3' ......................................................1
Wrench or Socket 14mm, 17mm
To check/re-align pulleys:
1. DISCONNECT MACHINE FROM POWER!
2. Remove belt cover, then use straightedge
to check pulley alignment, as shown in
Figure 62.
................... 2 Ea.
Tensioning Table Height Chain
The table height chain is located under the table.
It transfers movement from the handwheel to
the columns that control table height. The chain
drive can be adjusted to remove slack if the chain
stretches over time or is loosened during table
leveling procedures.
Items Needed Qty
Phillips Screwdriver #2 ........................................1
Wrench or Socket 14mm
To tension table height chain:
1. DISCONNECT MACHINE FROM POWER!
2. Remove motor access panel to access table
height chain (see Figure 63).
3.
Loosen both chain-tension lock bolts (see
Figure 63), then push idler sprocket against
chain with moderate pressure to eliminate
slack in chain. While maintaining pressure
on idler sprocket, re-tighten lock bolts.
....................................... 1
— If pulleys are parallel and in the same
plane, no adjustment is necessary. Reinstall belt cover.
— If pulleys are not parallel or in the same
plane, remove motor access panel, then
proceed to Step 3.
3.
Loosen (4) motor mount bolts, shift motor
until pulleys are aligned, then re-tighten
bolts.
4.
Re-check pulleys and repeat Step 3 as
necessary until you are satisfied with pulley
alignment, then re-tighten all fasteners, and
replace belt cover and motor access panel.
-44-
4. Clean and lubricate chain and sprockets
(refer to Table Height Chain & Sprockets
on Page 36 for detailed instructions), then
re-install motor access panel.
NOTICE
DO NOT let chain fall off sprockets. It can
be very difficult to return chain to its proper
location on sprockets without changing table
adjustments.
Page 50
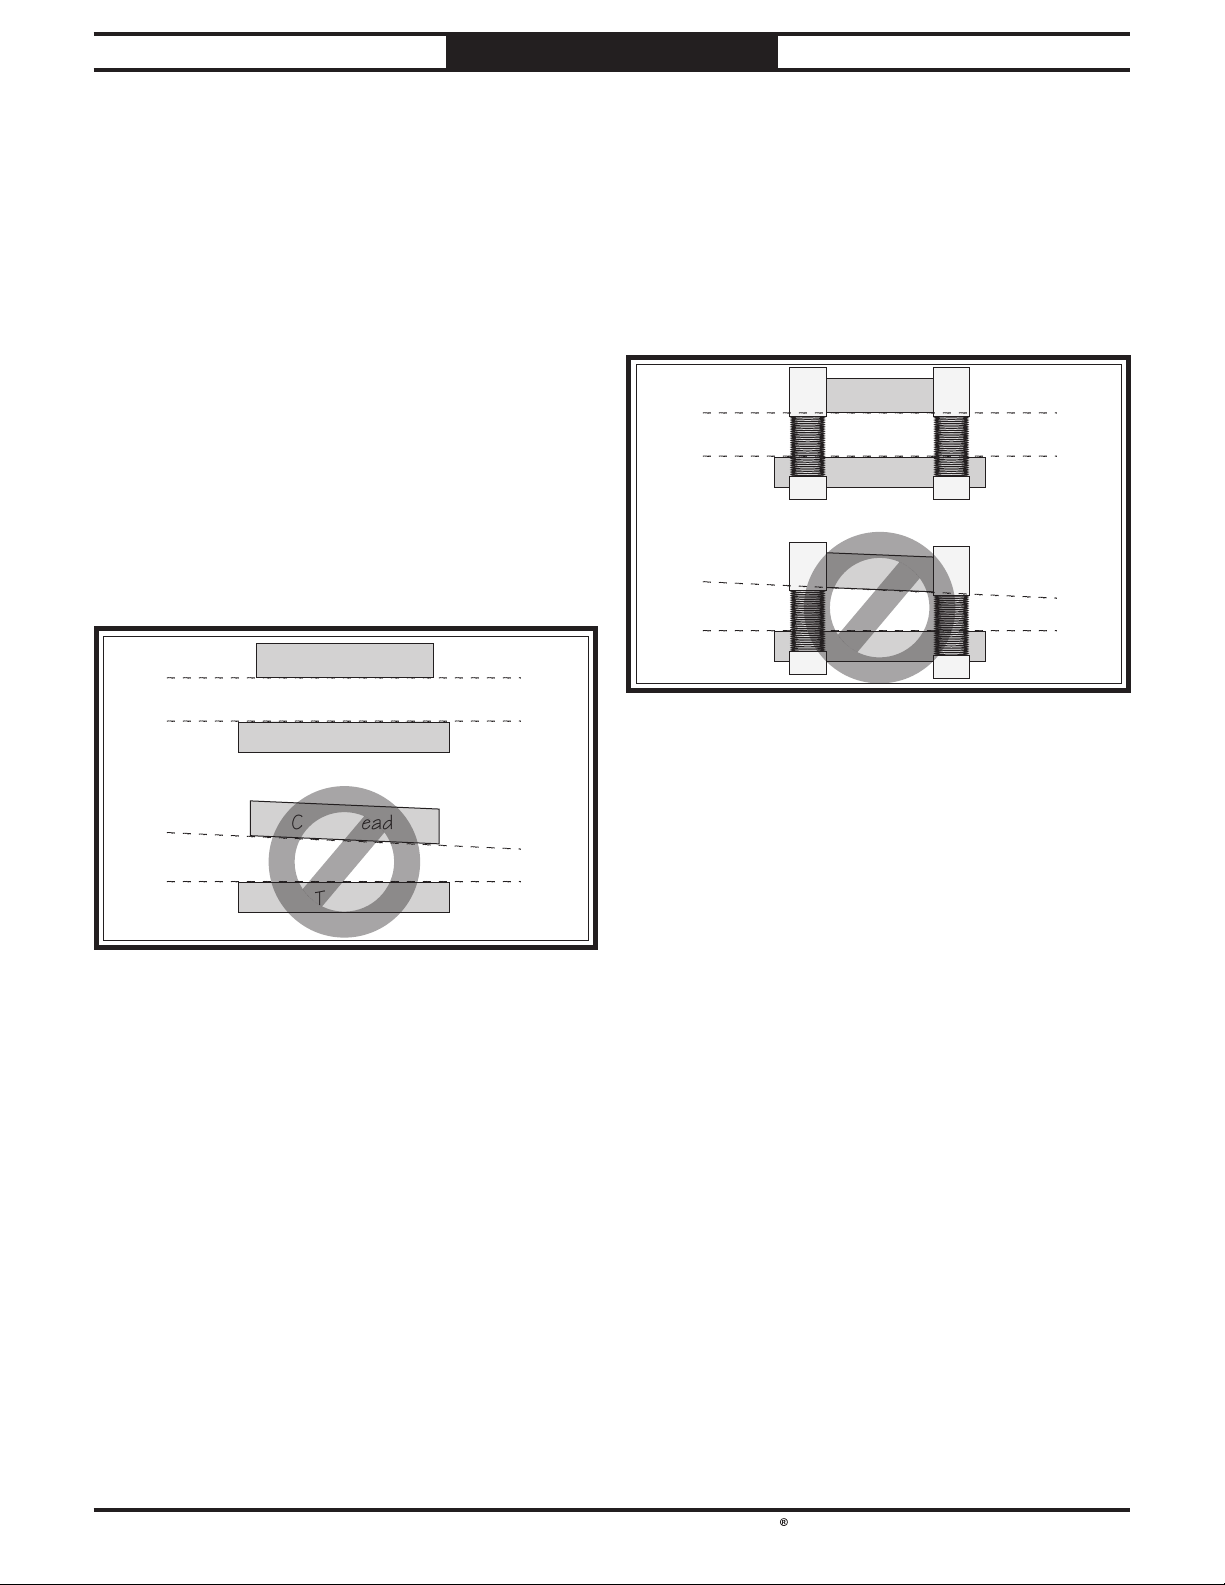
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
SERVICE
Adjusting Table Parallelism
Maximum Allowable Tolerances
Cutterhead/Table Side-to-Side
Head Casting/Table Front/Back
Tools Needed Qty
Rotacator ...............................................................1
Phillips Screwdriver #2
Wrench or Socket 14mm
Hex Wrench 6mm
Table parallelism is critical to the operation of
the machine. As such, it is essential that the
table is adjusted parallel with the cutterhead
(within 0.002") from side-to-side, as illustrated in
Figure 64.
........................................1
.................................................1
Cutterhead
.....................0.002"
...................0.020"
....................................... 1
How the table sits in relation to the head casting
from front-to-back is also important. Because the
feed rollers, pressure bar, and chip breaker are
adjusted off the table position, the tolerances on
the front-to-back positioning are not as critical
as the cutterhead/table side-to-side positioning.
Therefore, the maximum allowable tolerance for
the front-to-back parallelism is within 0.020" (see
Figure 65).
Head
Parallel Parallel
Table
FRONT BACK
Head
Not Parallel Not Parallel
Table
Parallel Parallel
Table
SIDE-TO-SIDE
Cutterhead
Not Parallel Not Parallel
Table
FRONT
VIEW
Table Parallelism Inspection
The easiest way to determine if your head
casting has a parallelism problem is to plane a
workpiece and measure the thickness in multiple
locations. If the workpiece is tapered from left-toright or from front-to-back, then parallelism may
be a problem.
Use your Rotacator to further inspect the table
parallelism. If you do not have a Rotacator, a
wood block and feeler gauges may be used, but
extra care must be taken to ensure accuracy. If
the table is not within the maximum allowable
tolerances, it must be adjusted.
-45-
Page 51
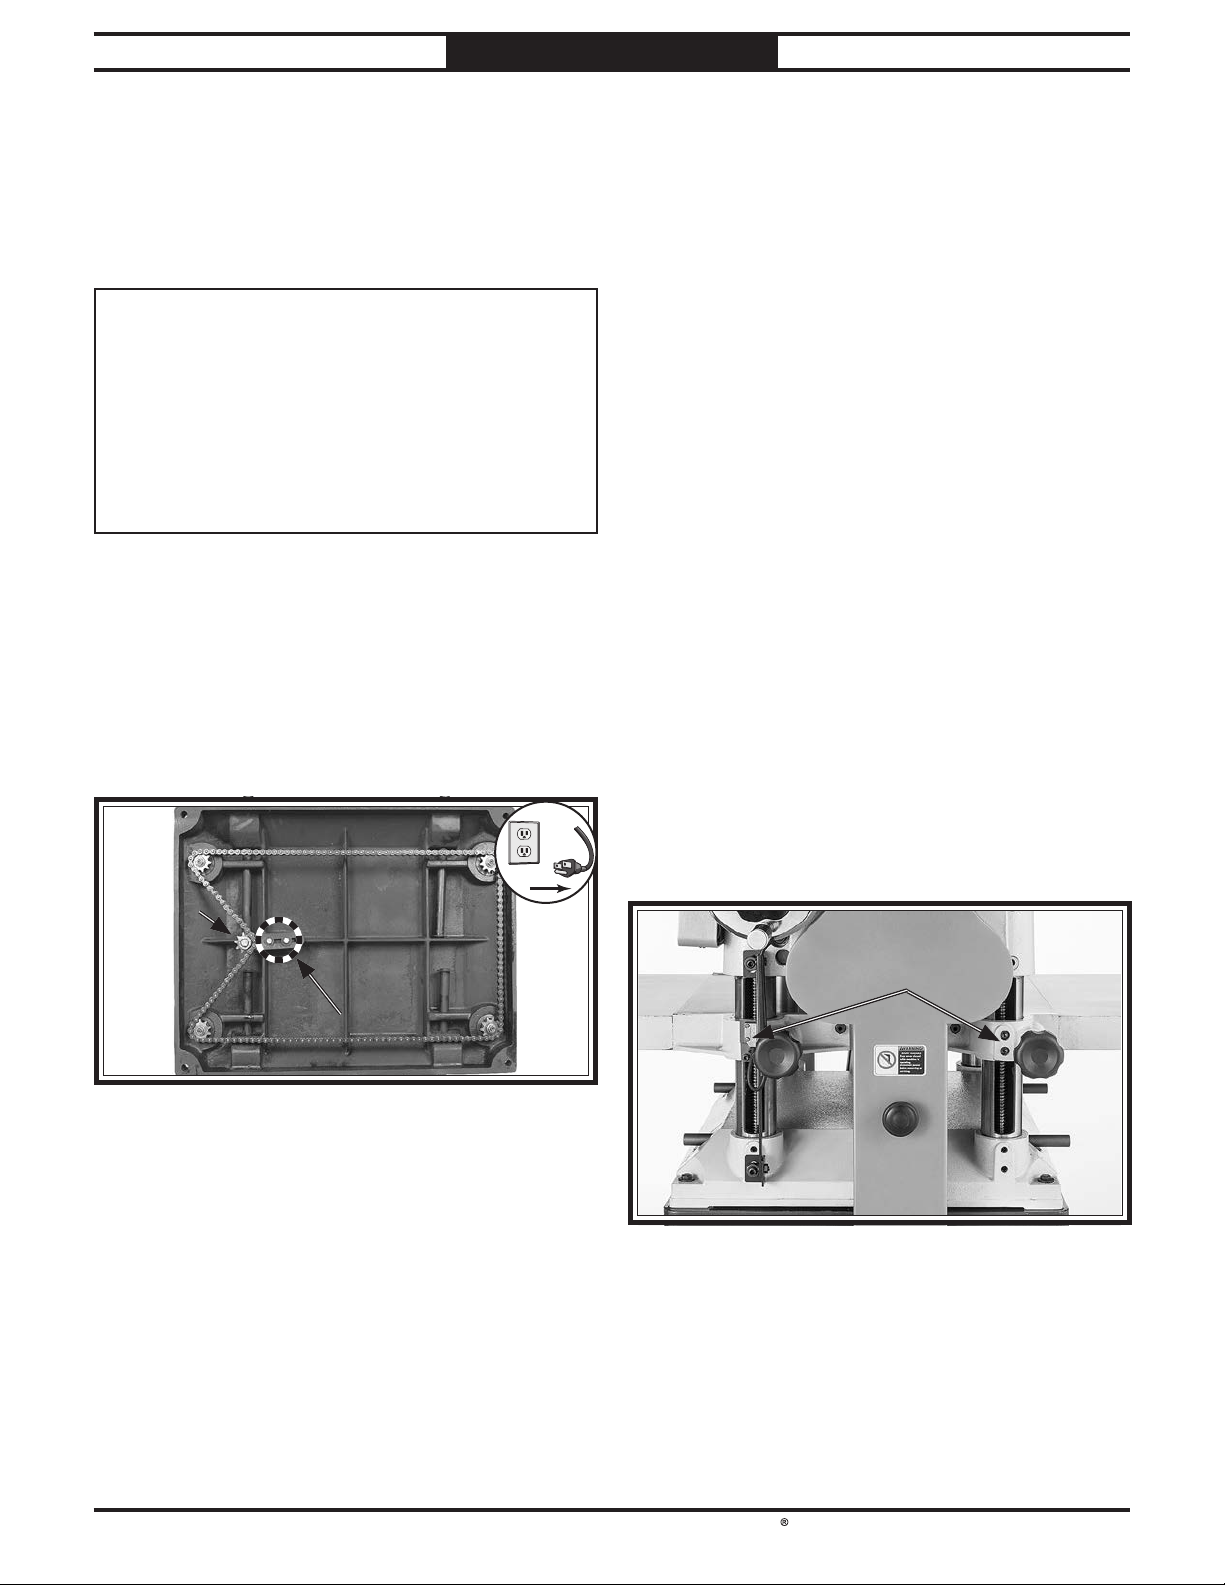
South Bend Tools
Model SB1108/ SB1109
!
SERVICE
For Machines Mfd. Since 12/20
Table Parallelism Adjustments
The table is adjusted by turning the chain
sprockets underneath the table for movements
over 0.016" or by adjusting how the table is
mounted on the columns for movements under
0.016".
NOTICE
When making adjustments, tighten fasteners
after each step to ensure the accuracy of your
tests. When adjusting the chain sprockets,
keep in mind that if the chain becomes too
loose, it will fall off of all the sprockets, and
returning it to its proper location can be
extremely difficult.
To adjust table parallelism:
DISCONNECT MACHINE FROM POWER!
1.
Remove motor access panel and locate chain
2.
on underside of table.
Loosen lock bolts and idler sprocket (see
3.
Figure 66).
5. Mark location of one tooth of sprocket that
you are adjusting.
Carefully rotate sprocket (clockwise to lower
6.
table; counterclockwise to raise table) just
enough to position next tooth at marked
location, then fit chain around sprocket
again.
Repeat Steps 4–6 with each sprocket
7.
that needs to be adjusted until table-tocutterhead clearance is within 0.016" from
one side to the other.
8. Make sure chain is properly fitted on
sprockets, then re-tighten idler sprocket and
lock bolts.
If necessary, micro-adjust table position by
9.
loosening cap screws (see Figure 67) and
raising or lowering table until it is properly
aligned with cutterhead.
Note: This process may require adjusting the
columns on both the left and right hand sides
until you find the correct combination.
4. Move chain away from sprocket you want to
adjust so only that sprocket can be rotated
independent of chain.
Note: If the left side of the table is too high,
the left two sprockets will need to be adjusted.
Each tooth on the sprocket represents 0.016"
of vertical movement as the cogs are turned.
Make sure, as you turn the sprockets, to keep
an accurate tooth count to ensure that the
table is adjusted equally.
Re-tension table height chain (see
10.
Tensioning Table Height Chain
instructions on Page 44).
-46-
Page 52
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
TROUBLESHOOTING
TROUBLESHOOTING
If you need replacement parts, or if you are unsure how to do any of the solutions given here, feel free
to call us at (360) 734-1540.
Symptom Possible Cause Possible Solution
Machine does not
start or power
supply breaker
immediately trips
after startup.
Machine stalls or is
underpowered.
1.
EMERGENCY STOP button
depressed/at fault.
2.
Machine circuit breaker tripped.
3.
Incorrect power supply voltage or
circuit size.
4.
Power supply circuit breaker
tripped or fuse blown.
5.
Thermal overload relay has tripped/
at fault.
6.
Start capacitor at fault.
7.
Contactor not energized/at fault.
8.
Wiring broken, disconnected, or
corroded.
9.
Start button or circuit breaker
switch at fault.
10.
Centrifugal switch adjustment/
contact points at fault.
11.
Pulse width modulator circuit board
at fault.
12.
Motor or motor bearings at fault.
1.
Workpiece material not suitable for
machine.
2.
Feed rate/cutting speed too fast.
3.
Belts slipping/pulleys misaligned.
4.
Pulley/sprocket slipping on shaft.
5.
Machine undersized for task.
6.
Motor overheated, tripping machine
circuit breaker.
7.
Run capacitor at fault.
8.
Extension cord too long.
9.
Contactor not energized/at fault.
10.
Centrifugal switch/contact points
at fault.
11.
Motor or motor bearings at fault.
1.
Rotate EMERGENCY STOP button head to reset.
Replace if at fault.
2.
Reset circuit breaker on control panel.
3.
Ensure correct power supply voltage and circuit
size.
4.
Ensure circuit is free of shorts. Reset circuit breaker
or replace fuse.
5.
Reset. Adjust or replace if at fault.
6.
Test/replace if at fault.
7.
Test all legs for power; replace if necessary.
8.
Fix broken wires or disconnected/corroded
connections.
9.
Replace button/circuit breaker switch.
10.
Adjust centrifugal switch/clean contact points.
Replace either if at fault.
11.
Inspect; replace if at fault.
12.
Replace motor.
1.
Only cut wood/ensure moisture is below 20%
(Page 25).
2.
Decrease feed rate/cutting speed (Page 28).
3.
Clean/tension/replace belts (Page 38) ; ensure
pulleys are aligned (Page 44).
4.
Tighten/replace loose pulley/shaft.
5.
Use sharp inserts; reduce feed rate/depth of cut.
6.
Clean motor/let cool, and reduce workload. Reset
breaker.
7.
Test/repair/replace.
8.
Move machine closer to power supply; use shorter
extension cord.
9.
Test all legs for power; repair/replace if at fault.
10.
Adjust centrifugal switch/clean contact points.
Replace either if at fault.
11.
Replace motor.
Feed motor does
not start or stalls.
1.
Motor brushes worn out.
1.
Replace motor brushes (Page 43).
-47-
Page 53
South Bend Tools
Model SB1108/ SB1109
TROUBLESHOOTING
For Machines Mfd. Since 12/20
Symptom Possible Cause Possible Solution
Machine has
excessive vibration
or noisy operation.
Table is hard to
adjust.
Workpiece stops/
slows in the middle
of cut.
1.
Motor or component loose.
2.
Machine feet not adjusted properly.
3.
V-belts worn, loose, pulleys
misaligned or belt slapping cover.
4.
Cutterhead inserts at fault.
5.
Pulley loose.
6.
Motor mount loose/broken.
7.
Motor fan rubbing on fan cover.
8.
Bed rollers protruding unevenly.
9.
Cutterhead bearings at fault.
10.
Centrifugal switch.
11.
Motor bearings at fault.
12.
Plastic chip deflector hitting
inserts.
1.
Table locks are engaged or partially
engaged.
1.
Depth of cut too deep.
2.
Pitch and glue build-up on planer
components.
3.
One or both bed rollers are set too
low.
4.
Chip breaker or pressure bar set
too low.
5.
Feed rollers set too low or too high.
1.
Replace damaged or missing bolts/nuts or tighten if
loose.
2.
Adjust machine feet to stabilize machine.
3.
Inspect/replace belts with a new matched set
(Page 38). Realign pulleys if necessary (Page 44).
4.
Rotate/replace inserts (Page 30).
5.
Secure pulley on shaft.
6.
Tighten/replace.
7.
Fix/replace fan cover; replace loose/damaged fan.
8.
Adjust bed rollers (Page 29).
9.
Replace bearing(s)/realign cutterhead.
10
Test/repair/replace.
11.
Test by rotating shaft; rotational grinding/loose
shaft requires bearing replacement.
12.
Replace chip deflector and realign (Page 42).
1.
Completely loosen table locks.
1.
Reduce depth of cut (Page 28).
2.
Clean planer components with a pitch/resin
dissolving solvent.
3.
Raise height of bed rollers (Page 29).
4.
Raise height of chip breaker or pressure bar
(Page 39).
5.
Adjust feed rollers to correct height (Page 39).
Excessive snipe
(gouge at the end
of workpiece that
is uneven with the
rest of cut).
Note: A small
amount of snipe is
inevitable with all
types of planers–
the key is to
minimize it.
1.
One or both bed rollers are set too
high.
2.
Rear extension table slopes down or
is not level with main table.
3.
Chip breaker, feed roller, or
pressure bar set too low.
4.
Workpiece is not properly supported
as it leaves planer.
1.
Lower height of bed rollers (Page 29).
2.
Adjust rear extension table set screws to make
extension table level with main table (Page 19).
3.
Adjust height of chip breaker, feed roller, or
pressure bar (Page 39).
4.
Use an assistant or roller beds/stands to properly
support workpiece as it leaves planer.
-48-
Page 54
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
TROUBLESHOOTING
Symptom Possible Cause Possible Solution
Consistent
chipping pattern.
Fuzzy grain.
Glossy surface.
Long lines or ridges
that run the length
of workpiece.
Uneven cutting
marks, wavy
surface, or chatter
marks across face
of workpiece.
1.
Knots or conflicting grain direction
in workpiece.
2.
Nicked, chipped, or dull insert.
3.
Feed rate too fast.
4.
Depth of cut too deep.
5.
Bed rollers set too high or low; not
even with each other.
6.
Misaligned chip breaker.
1.
Workpiece has high moisture
content or surface wetness.
2.
Dull inserts.
1.
Inserts are dull.
2.
Feeding workpiece too slow.
3.
Cutting depth too shallow.
1.
Nicked or chipped inserts.
1.
Feed rate too fast.
2.
Chip breaker or pressure bar set
unevenly.
3.
Bed rollers set too high or low; not
even with each other.
4.
Insert(s) not properly installed.
5.
Worn cutterhead bearings.
1.
Inspect workpiece for knots and grain direction; use
only clean stock (Page 25).
2.
Rotate/replace insert (Page 30).
3.
Reduce feed rate (Page 28).
4.
Reduce depth of cut (Page 28).
5.
Properly adjust bed roller height (Page 29).
6.
Adjust both sides of chip breaker to correct height
(Page 39).
1.
Allow workpiece to dry if moisture content is over
20% or has high surface wetness.
2.
Rotate/replace inserts (Page 30).
1.
Rotate/replace inserts (Page 30).
2.
Increase feed rate (Page 28).
3.
Increase depth of cut (Page 28).
1.
Rotate/replace inserts (Page 30).
1.
Reduce feed rate (Page 28).
2.
Adjust height of chip breaker or pressure bar
(Page 39).
3.
Properly adjust bed roller height (Page 29).
4.
Remove insert(s), then properly clean and re-install
(Page 30).
5.
Replace cutterhead bearings.
Inconsistent chip
marks.
Workpiece twists
in machine.
1.
Chips are not being properly
expelled from around cutterhead.
1.
Pressure bar set unevenly.
2.
Bed rollers not parallel with table.
1.
Use an adequate dust collection system; adjust
chip deflector in or out, depending on your setup
(Page 39).
1.
Adjust height of pressure bar (Page 39).
2.
Adjust bed roller height (Page 29).
-49-
Page 55
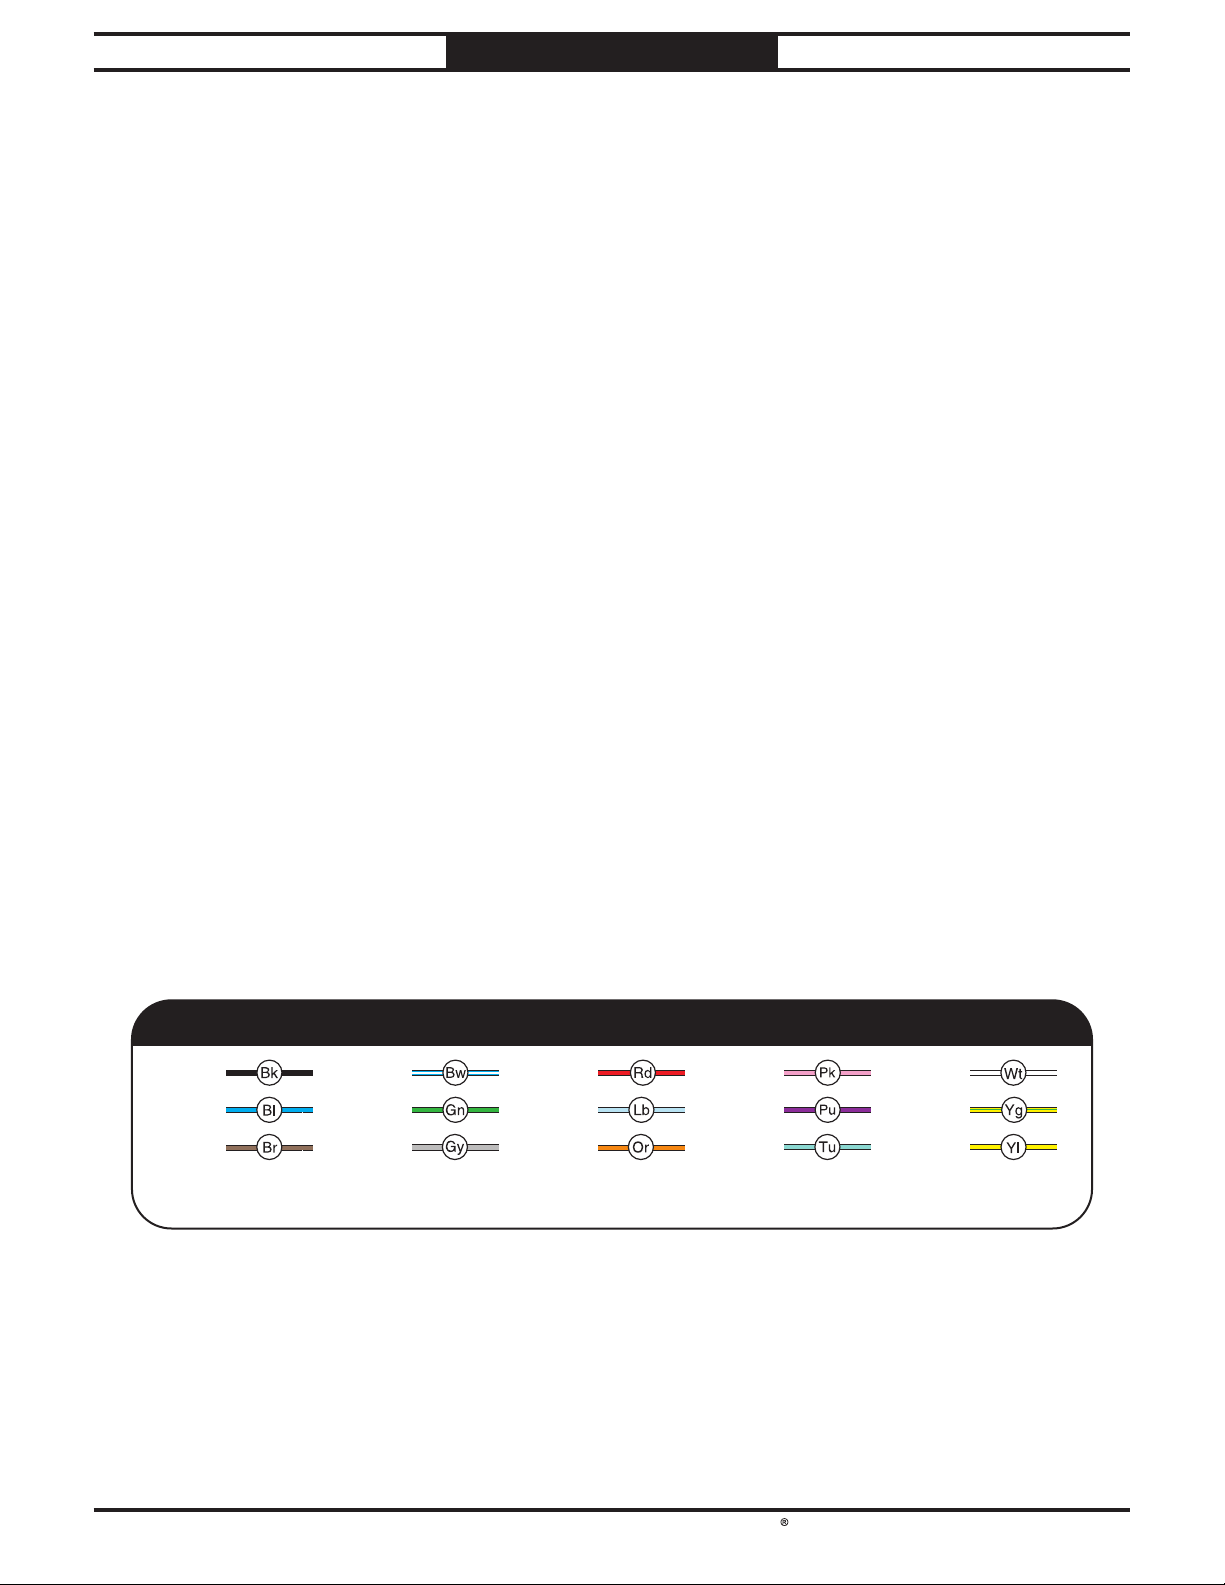
South Bend Tools
Model SB1108/ SB1109
Shock Hazard: It is extremely dangerous to
Wire Connections:
Modifications:
Motor Wiring:
junction box.
Circuit Requirements: Connecting the machine
power inverters store an electrical charge for
our Technical Support at (360) 734-1540.
ELECTRICAL
ELECTRICAL
For Machines Mfd. Since 12/20
Electrical Safety Instructions
These pages are accurate at the time of printing. In the constant effort to improve, however, we may
make changes to the electrical systems of future machines. Study this section carefully. If you see
differences between your machine and what is shown in this section, call Technical Support at (360)
734-1540 for assistance BEFORE making any changes to the wiring on your machine.
perform electrical or wiring tasks while the
machine is connected to the power source.
Touching electrified parts will result in
personal injury including but not limited to
severe burns, electrocution, or death. For
your own safety, disconnect machine from
the power source before servicing electrical
components or performing any wiring tasks!
All connections must be
tight to prevent wires from loosening during
machine operation. Double-check all wires
disconnected or connected during any wiring
task to ensure tight connections.
Using aftermarket parts or
modifying the wiring beyond what is shown
in the diagram may lead to unpredictable
results, including serious injury or fire.
The motor wiring shown in these
diagrams is current at the time of printing,
but it may not match your machine. Always
use the wiring diagram inside the motor
to an improperly sized circuit will greatly
increase the risk of fire. To minimize
this risk, only connect the machine to a
power circuit that meets the minimum
requirements given in this manual.
Capacitors/Inverters: Some capacitors and
up to 10 minutes after being disconnected
from the power source. To reduce the risk of
being shocked, wait at least this long before
working on capacitors.
Wire/Component Damage: Damaged wires
or components increase the risk of serious
personal injury, fire, or machine damage. If
you notice that any wires or components are
damaged while performing a wiring task,
replace those wires or components before
completing the task.
Experiencing Difficulties: If you are
experiencing difficulties understanding the
information included in this section, contact
BLACK
BLUE
BROWN
NOTICE:
-50-
WIRING DIAGRAM COLOR KEY
BLUE
WHITE
GREEN
G R AY
The photos and diagrams included in this section are best viewed in color. You can
see them in color at www.southbendtools.com.
RED
LIGHT
BLUE
ORANGE
PINK
PURPLE
TURQUIOSE
WHITE
YEL LOW
GREEN
YEL LOW
Page 56
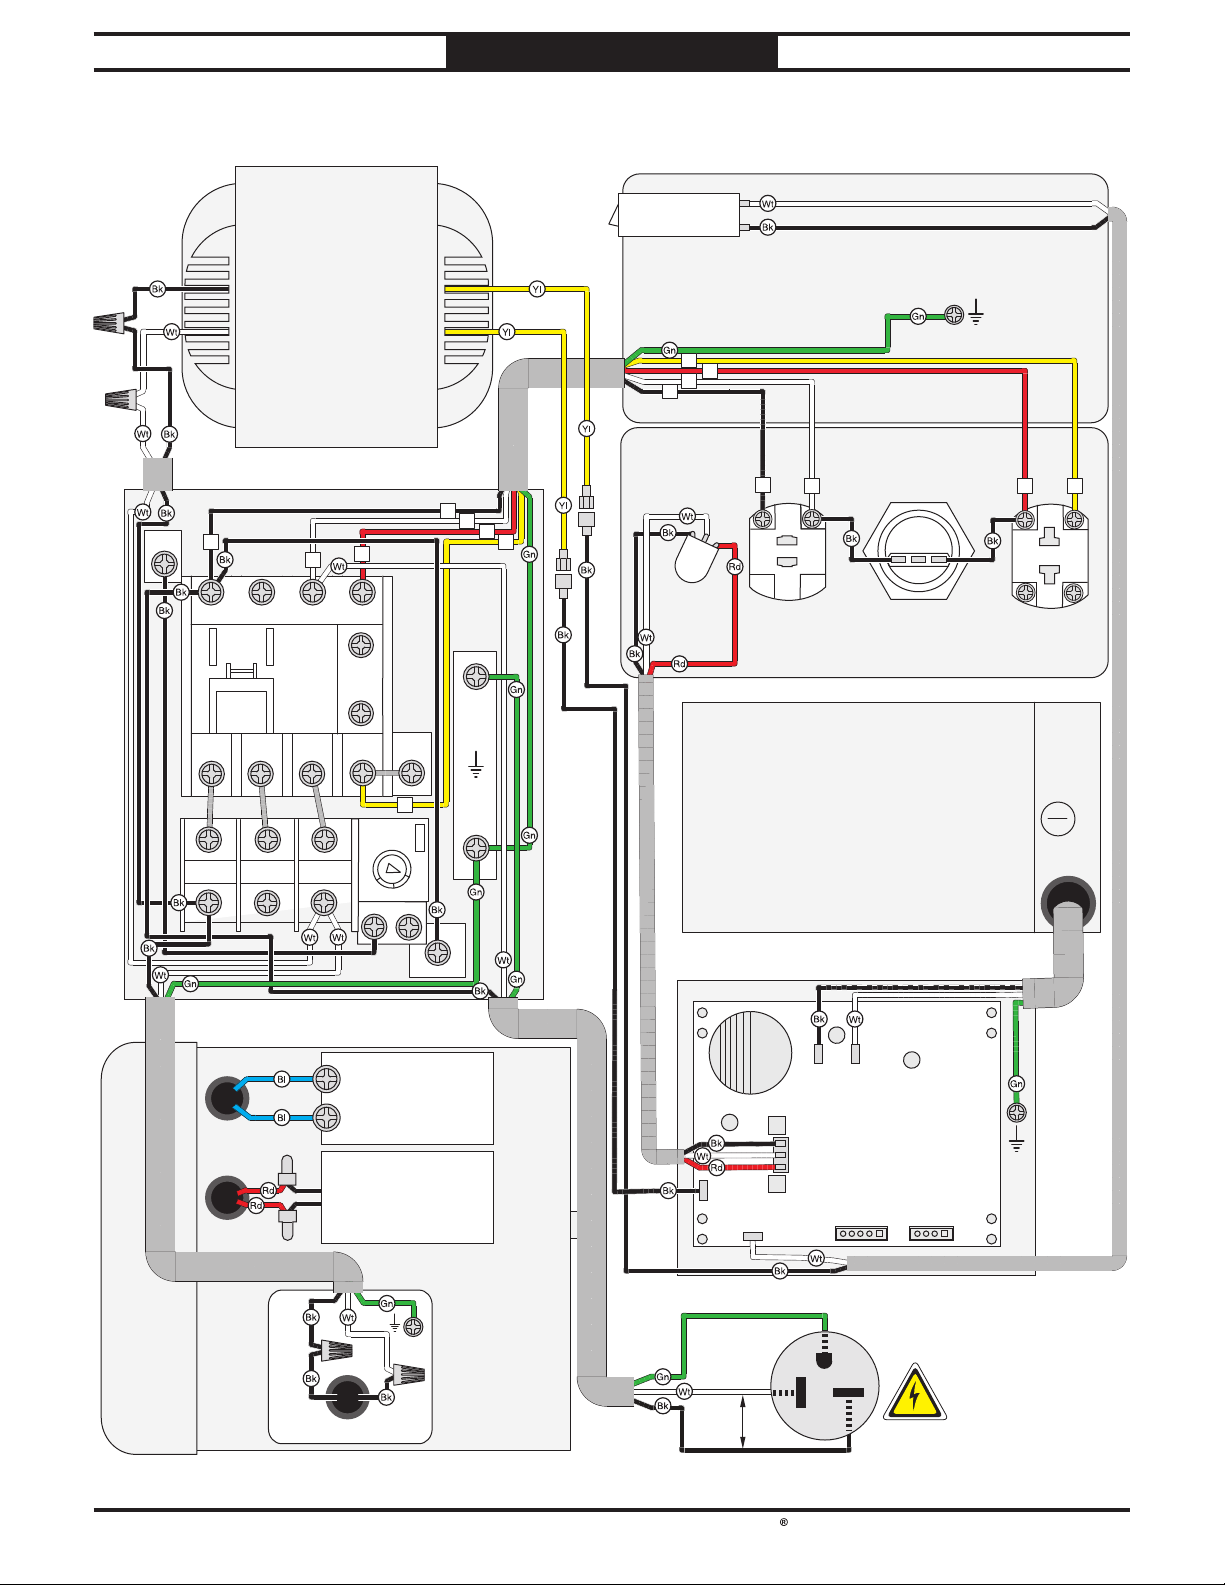
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
ELECTRICAL
SB1108 Wiring Diagram
ZING EAR
ZE-800 4A 250V
INPUT 220V(3A)
Transformer
SUENN LIANG
SP-CL-20660
OUTPUT 110V(6A)
Circuit Breaker
5
6
1
4
Magnetic Switch
4
A
L1/1
L2/3
SDE
MA-18
T2/4
T1/2 T3/6 NO14
1/2
3/4
SDE MPE-18
6
1
L3/5
NO13
NC 21
NC 22
5
RA-20
5/6
18
15
96
98
Main Motor
400MFD
125VAC
4
X1
250V 1.2W
YK
A600
Power
Indicator
1
X2
CNONC
RENY
E-Stop
Button
4
1
6
5
Potentiometer
B10K
1
13
10A250VAC
7.5A380VAC
A600
Start
Button
56
14
YK
Control Panel
GND
B
Feed Motor
RESET
12
95
Pulse Width Modulator
Circuit Board
C9
Start
Capacitor
LOW
M+
+
VR2
P2
M-
T4
T3
70uF
250VAC
Run
Capacitor
T1
AC1
Hot
220
VAC
High
T2
AC2
Ground
Hot
VR1
P1
P3
G
6-20 Plug
-51-
Page 57
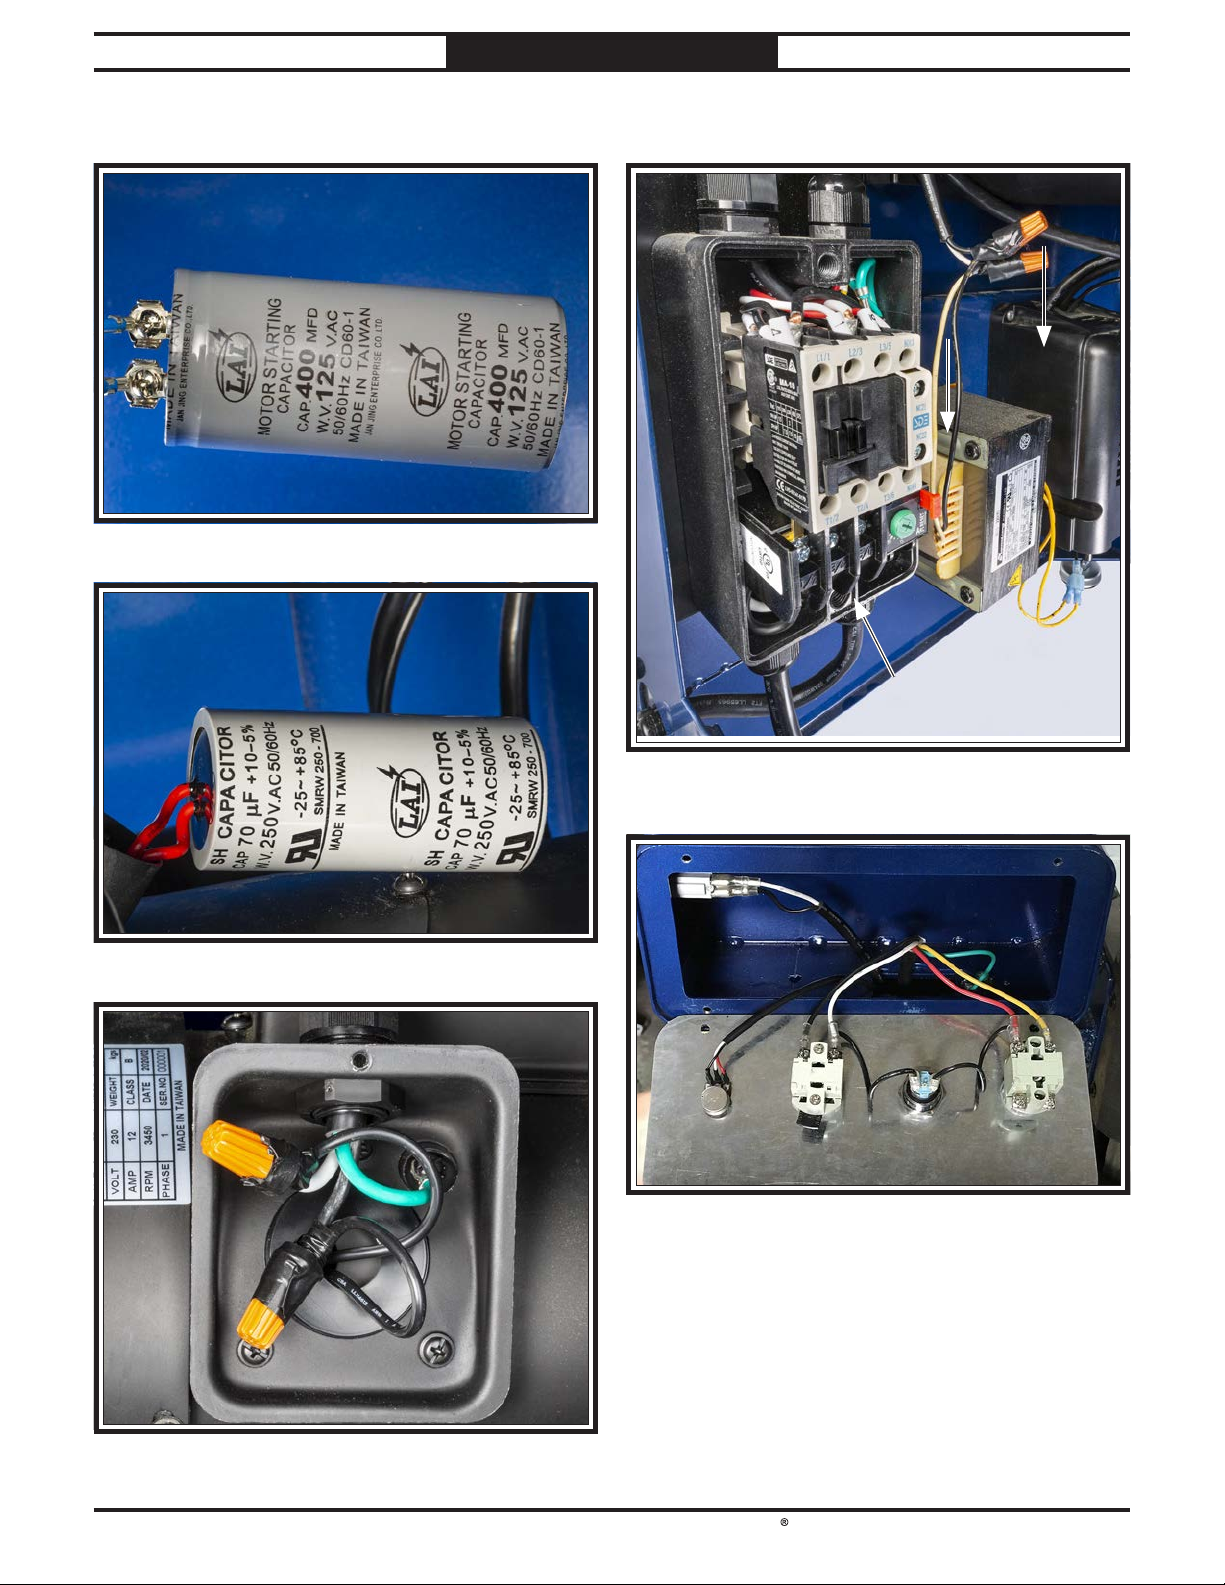
South Bend Tools
Model SB1108/ SB1109
ELECTRICAL
For Machines Mfd. Since 12/20
SB1108 Electrical Component Photos
width modulator.
-52-
Page 58
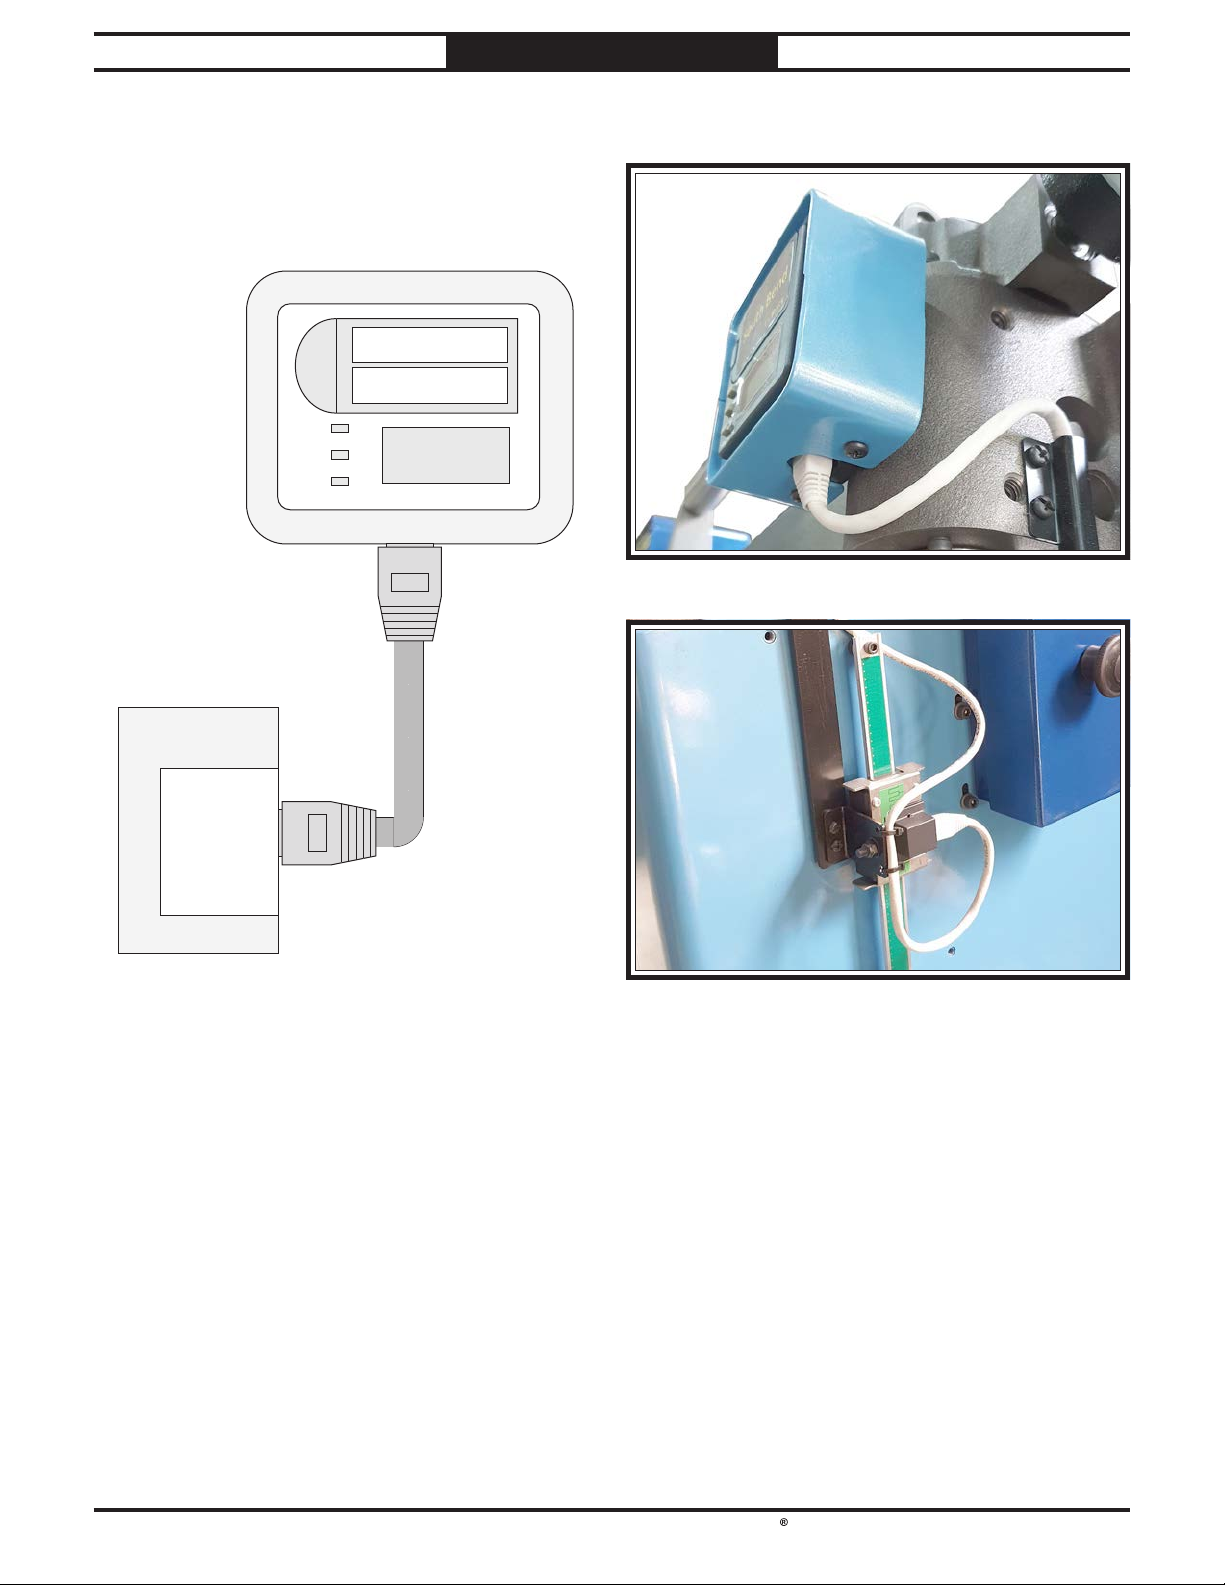
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
ELECTRICAL
SB1108 Height DRO Wiring Diagram
HEIGHT
DIGITAL
READOUT
AAA Battery
+
-
DRO HEIGHT
SENSOR
AAA Battery
+-
-53-
Page 59
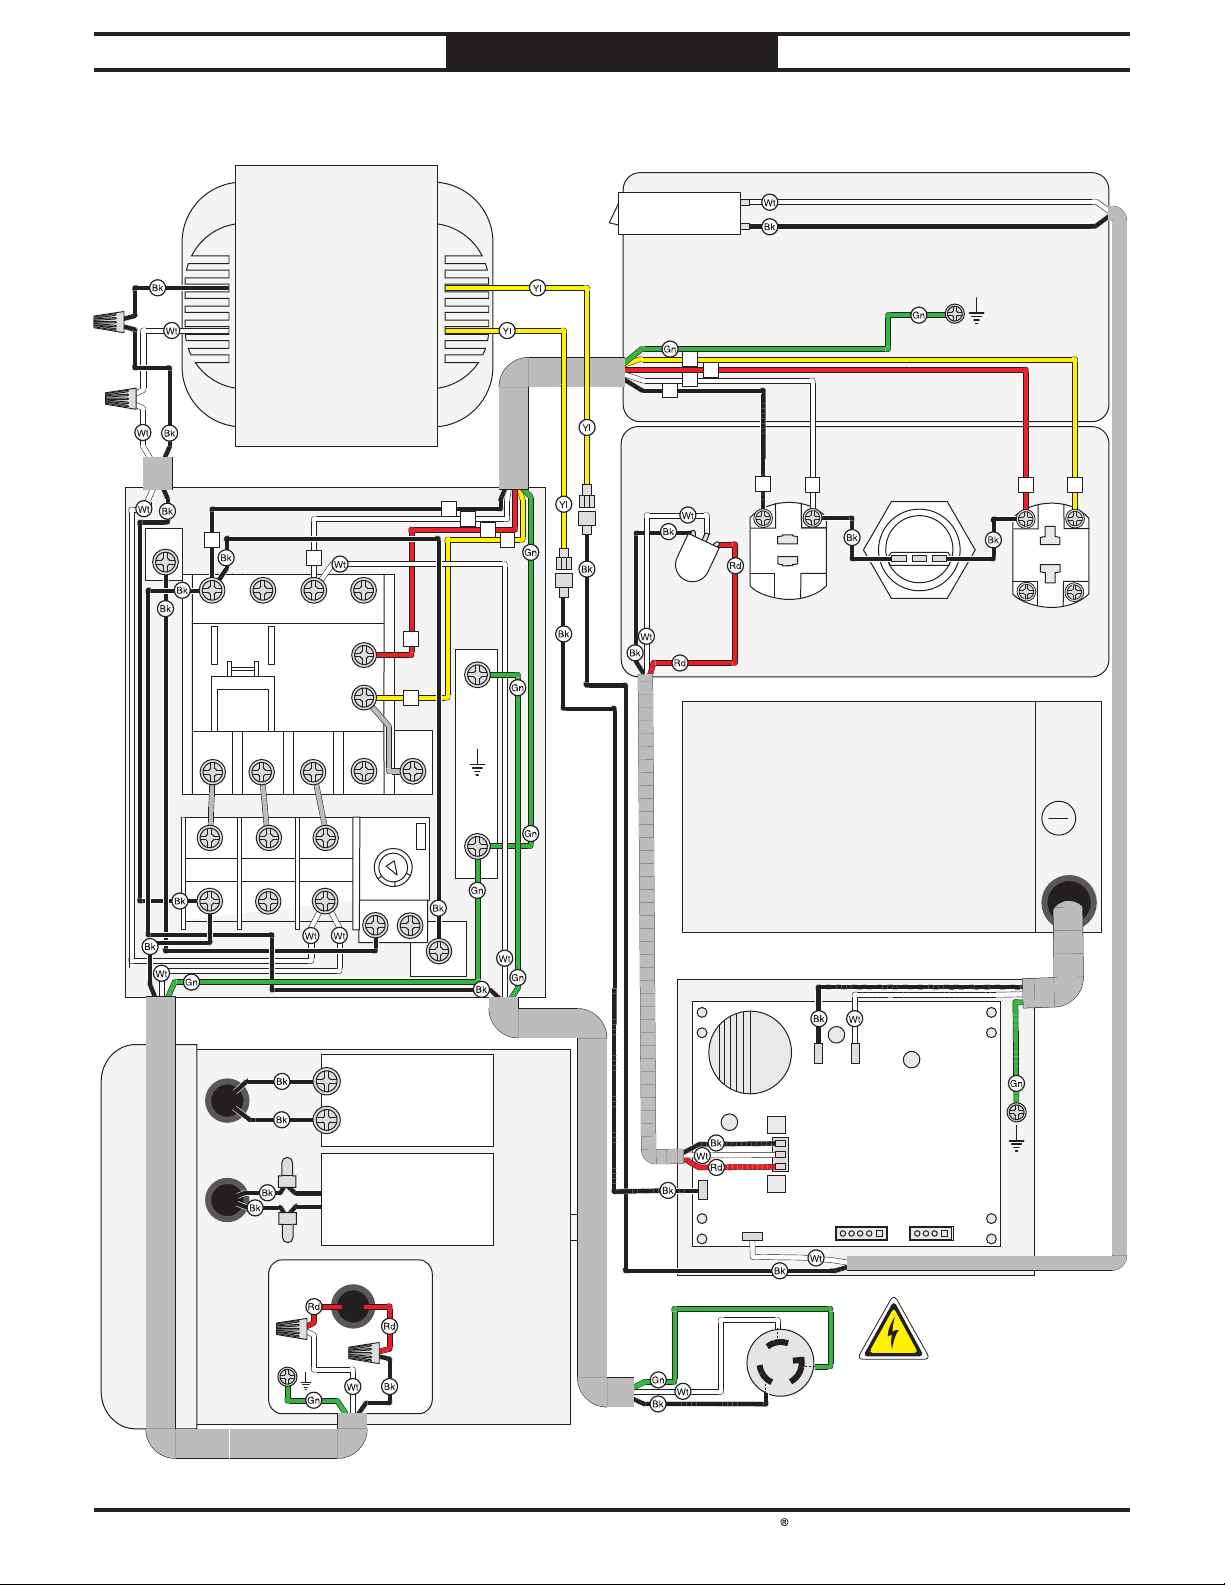
South Bend Tools
Model SB1108/ SB1109
ELECTRICAL
SB1109 Wiring Diagram
INPUT 220V(3A)
Transformer
SUENN LIANG
SP-CL-20660
OUTPUT 110V(6A)
ZING EAR
ZE-800 4A 250V
Circuit Breaker
5
6
1
4
For Machines Mfd. Since 12/20
Magnetic Switch
4
A
R/1/L1
SDE
MA-30
U/2/T1 W/6/T3
1/2
SDE MPE-30
1
S/3/L2
T/5/L3
V/4/T2
3/4
5/6
Main Motor
21
13
14
22
RA-30
34
96
600MFD
125VAC
4
X1
250V 1.2W
YK
A600
Power
Indicator
1
X2
CNONC
RENY
E-Stop
Button
4
1
6
5
6
Potentiometer
B10K
1
13
10A250VAC
7.5A380VAC
A600
Start
Button
56
14
YK
Control Panel
5
GND
B
Feed Motor
RESET
22
28
98
95
Pulse Width Modulator
Circuit Board
C9
Start
Capacitor
LOW
M+
+
VR2
P2
M-
T4
T3
-54-
60uF
350VAC
Run
Capacitor
T1
AC1
Ground
Hot
AC2
Hot
High
VR1
T2
X
Y
P1
P3
G
220 VAC
L6-30 PLUG
Page 60
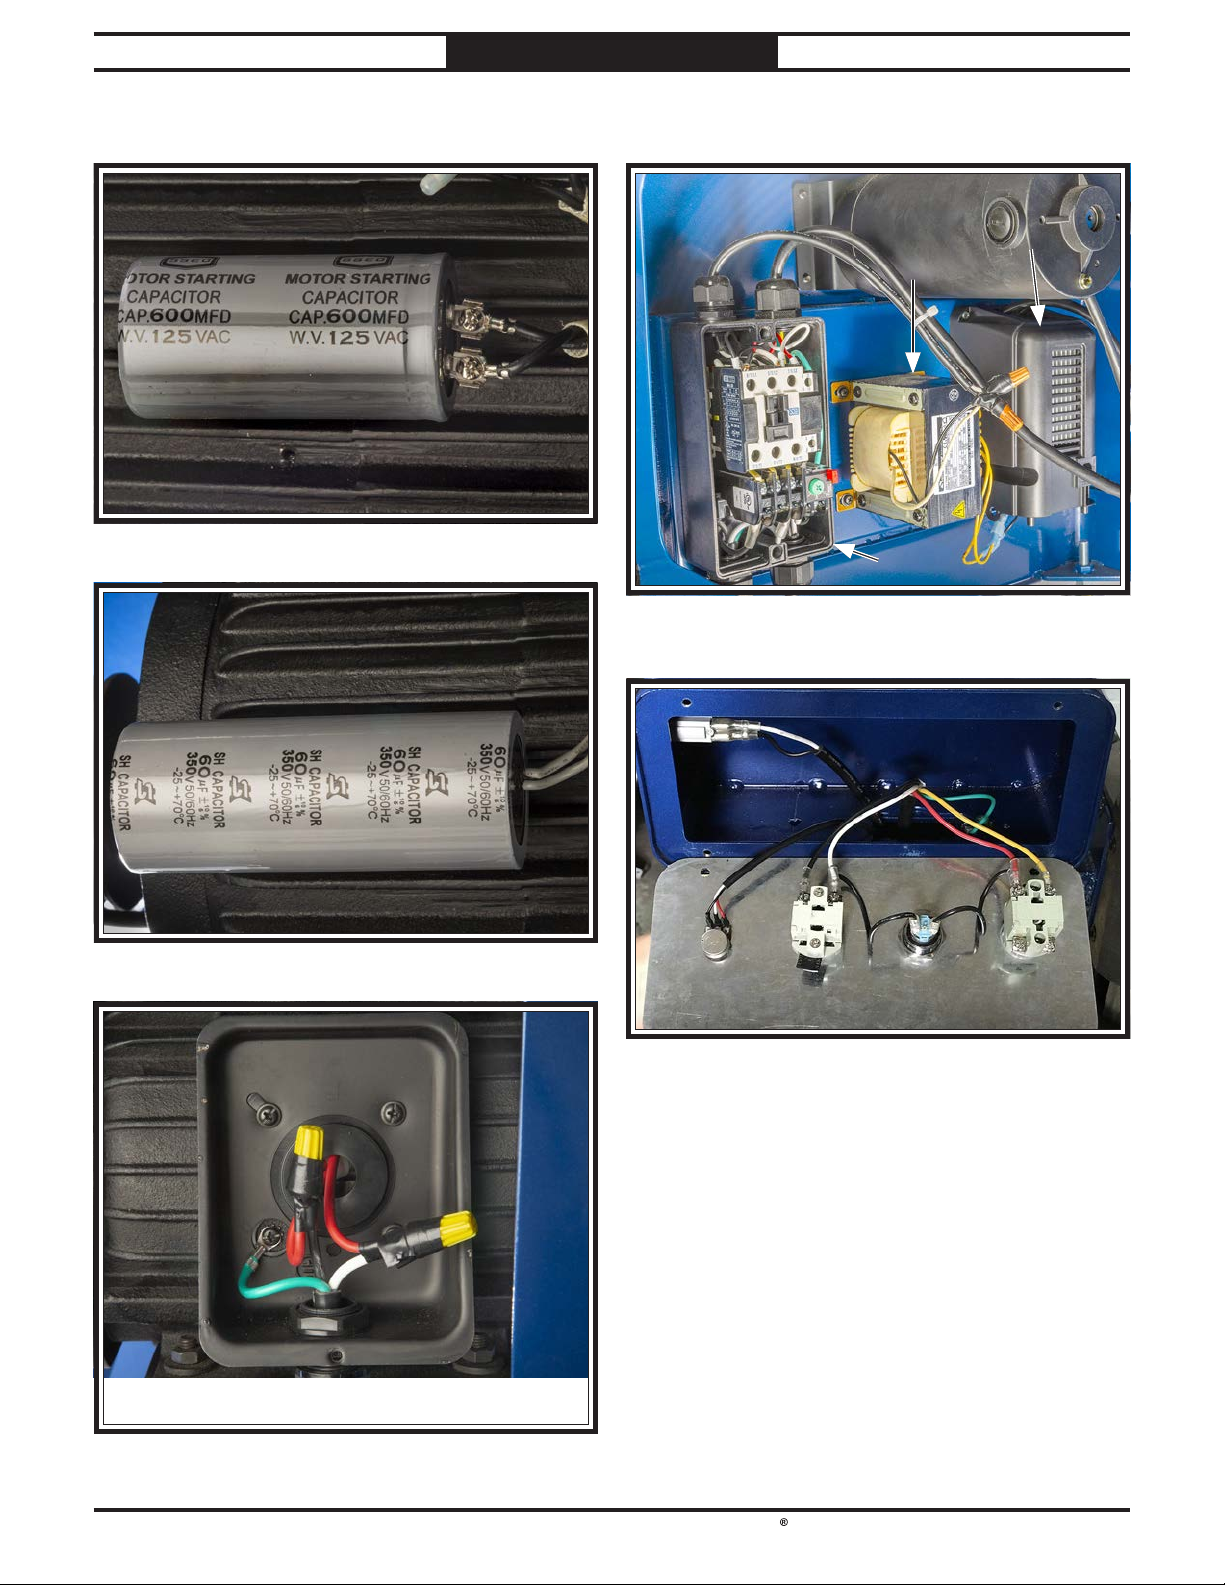
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
ELECTRICAL
SB1109 Electrical Component Photos
width modulator.
-55-
Page 61
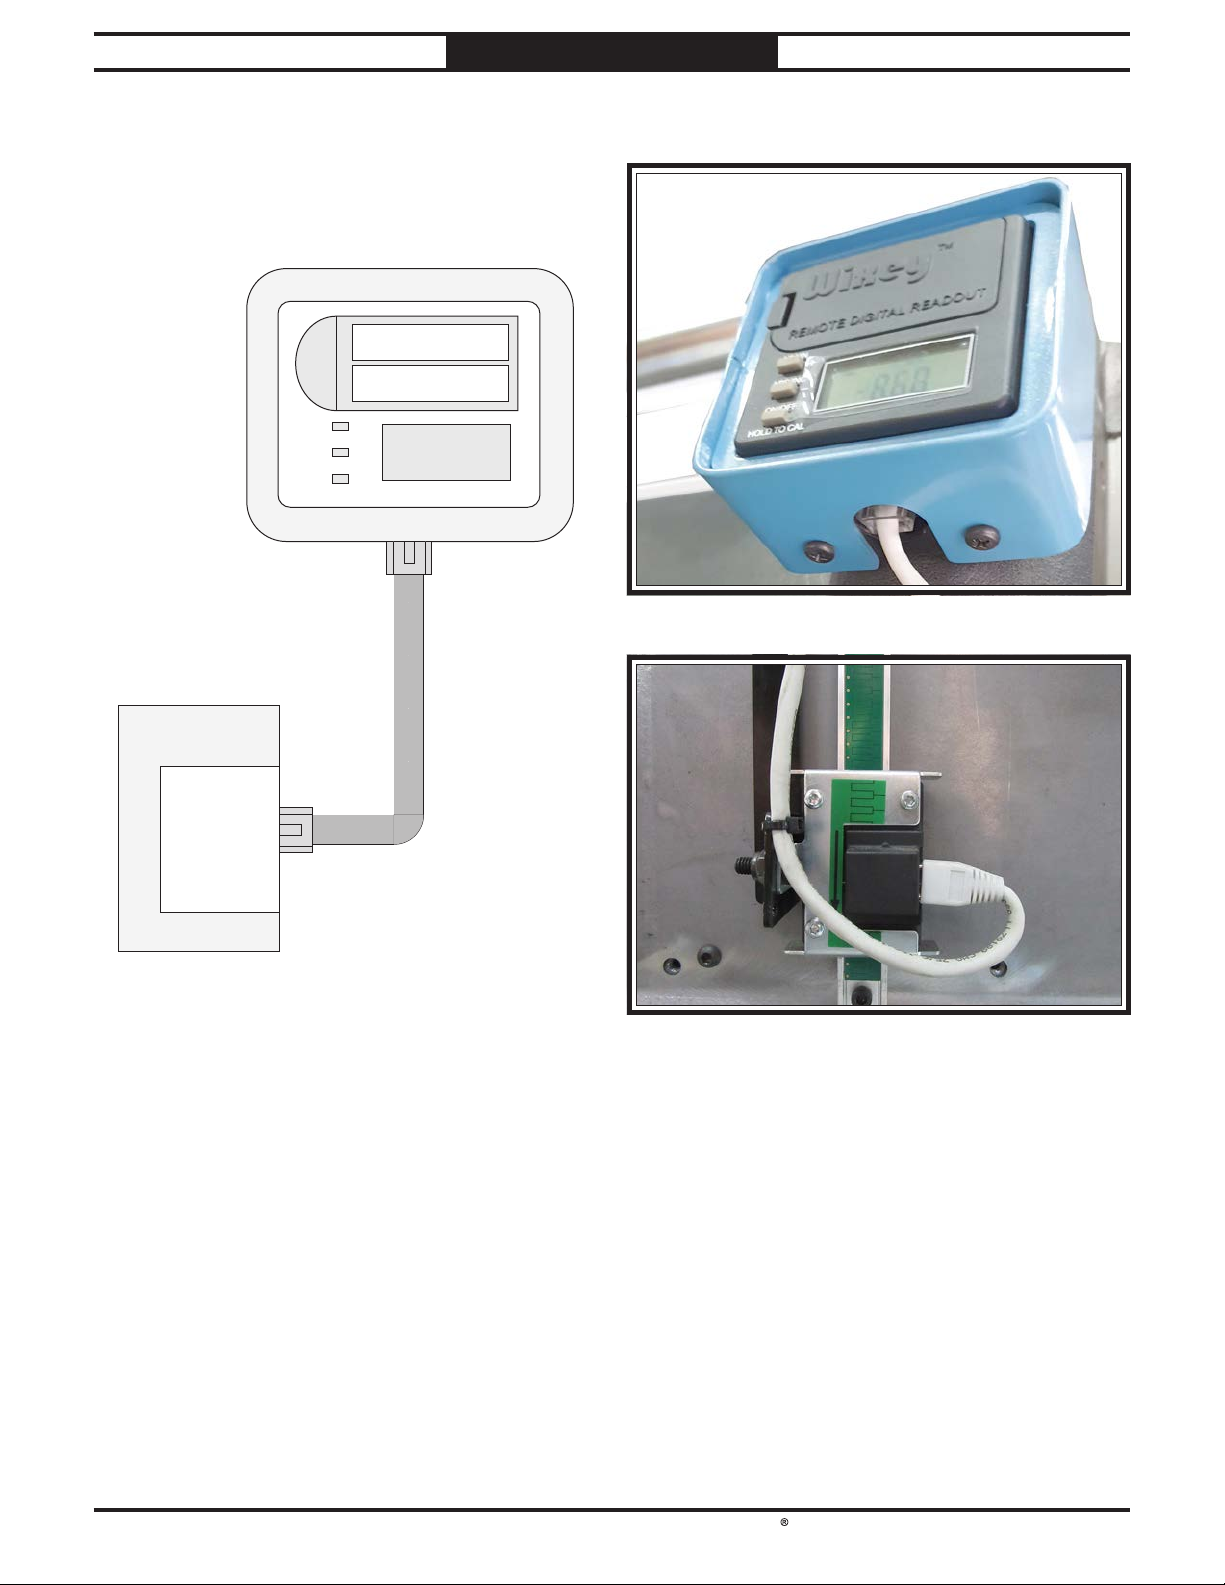
South Bend Tools
Model SB1108/ SB1109
ELECTRICAL
For Machines Mfd. Since 12/20
SB1109 Height DRO Wiring Diagram
HEIGHT
DIGITAL
READOUT
AAA Battery
+
-
DRO HEIGHT
SENSOR
AAA Battery
+-
-56-
Page 62
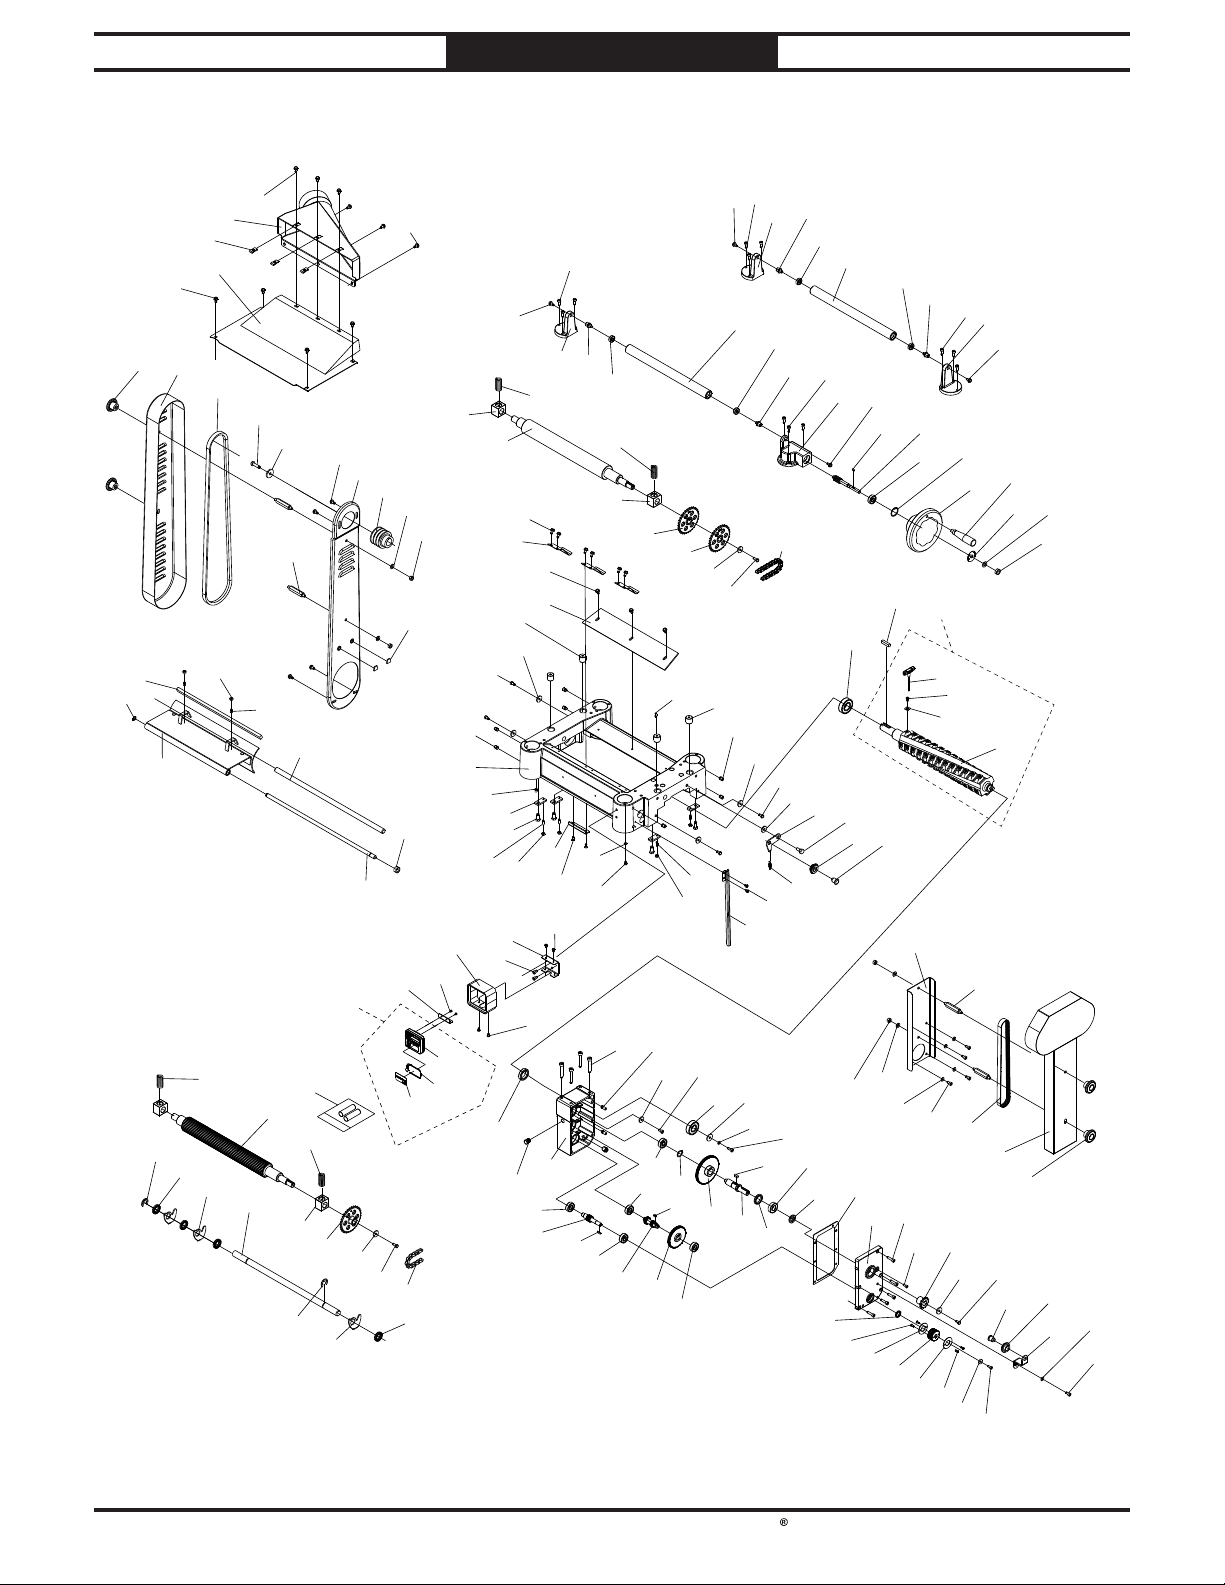
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PARTS
PARTS
SB1108 Main
16
69
84
82
34
212
77
85
33
78
54
36
8
86
20
34
221
79
80
87
17
19
55
35
220
88
18
43
48
81
18
44
202
203
19
89
16
95
20
21
45
12
57
46
96
90
8
106
91
11
97
22
47
58
19
105
92
96
23
77
93
24
95
18
56
16
56-1
56-2
56-3
107
94
98
79
25
26
56-4
208
108
93
17
8
27
28
29
30
1
35
46
47
207
106
77
109
224
1
114
223
8
15
14
13
8
2
3
4
6
7
69
42
110
64
49
115
116
72
113
49
117
50
118
114
116
8
34
111
9
54
10
112
64-3
67
119
8
11
37
12
115
50
65
64-1
64-2
63
36
38
39
212
35
62
51
41
40
73
31
33
61
99
8
34
69
8
220
82
101
32
49
8
59
220
100
17
60
102
16
18
50
205
204
82
19
49
103
74
52
82
53
42
75
76
82
83
104
-57-
Page 63
South Bend Tools
Model SB1108/ SB1109
PARTS
For Machines Mfd. Since 12/20
SB1108 Main Parts List
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
1 PSB1108001 KNOB 5/1 6-18 LOBED 53 PSB1108053 SPROCKET SIZE 31T
2 PSB1108002 BELT PULLEY COVER 54 PSB1108054 HEX BOLT M6-1 X 16
3 PSB1108003 V-B ELT M 58 55 PSB1108055 CHAIN #06B X 40P
4 PSB1108004 HEX BOLT M8-1.25 X 30 56 PSB1108056 HELICAL CUTTERHEAD ASSY
6 PSB1108006 FEN DER WASHER 8MM 56-1 PSB1108056-1 T-HANDLE TORX DRIVER T25
7 PSB1108007 STANDOFF-H EX MM 5.16-18 X 2-1/4, 3/8 56-2 PSB1108056-2 FLA T HD TORX 10-32 X 1/2
8 PSB1108008 FLAN GE BOLT M6-1 X 12 56-3 PSB1108056-3 INSERT 15 X 15 X 2.5MM-10 PK
9 PSB1108009 BELT PULLEY GUARD 56-4 PSB1108056-4 HELICAL CUTTERHEAD 15"
10 PSB1108010 PULLEY 57 PSB1108057 BA LL BEARING 6205-2N SE
11 PSB1108011 FLAT WASHER 8MM 58 PSB1108058 KEY 8 X 8 X 36 RE
12 PSB1108012 HEX NUT 5/16-18 59 PSB1108059 DEPTH LIMITER
13 PSB1108013 UPPER COVER 60 PSB1108060 FLAT H D SCR M5-.8 X 1 2
14 PSB1108014 CLIP-ON NUT M6-1 61 PSB1108061 DIGITAL READOUT BRACKET
15 PSB1108015 DUS T H OOD W/4" PORT 62 PSB1108062 CAP SCREW M6-1 X 10
16 PSB1108016 CAP SCREW M6-1 X 20 63 PSB1108063 DIGITAL READOUT HOUSIN G
17 PSB1108017 RETURN ROLLER B RAC KET 64 PSB1108064 DIGITAL READOUT ASS EMBLY
18 PSB1108018 BEARING SHAFT 64-1 PSB1108064-1 DIGITAL READOUT WIXEY WR5502
19 PSB1108019 BALL B EARING 608 Z 64-2 PSB1108064-2 BATTERY COVER
20 PSB1108020 RETURN ROLLER 64-3 PSB1108064-3 BATTERY COVER DECAL
21 PSB1108021 WORM GEAR HOUSING 65 PSB1108065 TAP S CREW M3 X 8
22 PSB1108022 KEY 4 X 4 X 10 RE 67 PSB1108067 MOUNTIN G PLA TE
23 PSB1108023 WORM SHAFT 69 PSB1108069 HEX N UT M6-1
24 PSB1108024 BALL B EARING 6200Z 72 PSB1108072 BATTERY AAA (2PC)
25 PSB1108025 INT RETAINING RING 30MM 73 PSB1108073 OIL SEAL 28 X 40 X 8
26 PSB1108026
27 PSB1108027 REVOLVING HANDLE 3/8 -16 X 1/2 75 PSB1108075 ROLL PIN 8 X 20
28 PSB1108028 DIRECTION LAB EL 76 PSB1108076 FEN DER WASHER 6MM
29 PSB1108029 FLAT WASHER 10MM 77 PSB1108077 CAP SCREW M6-1 X 12
30 PSB1108030 HEX NUT M10-1.25 78 PSB1108078 BA LL BEARING 6204-2NSE
31 PSB1108031 SPRIN G PLA TE 79 PSB1108079 FENDER WASHER 6MM
32 PSB1108032 CHIP DEFLECTOR 80 PSB1108080 LOCK WASHER 6MM
33 PSB1108033 OILER SCREW M22-1.5 X 20 81 PSB1108081 CAP SCREW M6-1 X 16
34 PSB1108034 FEN DER WASHER 6MM 82 PSB1108082 BALL B EARING 6201Z Z
35 PSB1108035 HEX BOLT M6-1 X 12 83 PSB1108083 EXT RETAINING RING 20MM
36 PSB1108036 SET SCREW M10-1.5 X 12 84 PSB1108084 KEY 5 X 5 X 10 RE
37 PSB1108037 PLATE 85 PSB1108085 GEAR 96T
38 PSB1108038 HEAD CASTING 86 PSB1108086 SHAFT SIZE 24.5 X 10⁵
39 PSB1108039 SET SCREW M8-1.25 X 10 87 PSB1108087 OIL SEAL 25 X 35 X 5
40 PSB1108040 HEX BOLT M8-1.25 X 20 88 PSB1108088 KEY 6 X 6 X 15 RE
41 PSB1108041 PLATE 89 PSB1108089 COLLAR
42 PSB1108042 S ET SCREW M6-1 X 12 90 PSB1108090 GASKET
43 PSB1108043 F ENDER WASH ER 8MM 91 PSB1108091 GEA RB OX COVER
44 PSB1108044 CHAIN TENSIONER 92 PSB1108092 CAP SCREW M6-1 X 25
45 PSB1108045 SHOULDER BOLT M8-1.25 X 14.5, 4 X 12 93 PSB1108093 CAP SCREW M5-.8 X 12
46 PSB1108046 IDLER WHEEL 94 PSB1108094 S PROCKET 12T
47 PSB1108047 IDLER SHAFT 95 PSB1108095 PHLP HD SCR M4-.7 X 10
48 PSB1108048 EXTENSION SPRING 1 X 8.5 X 35 96 PSB1108096 PULLEY COVER
49 PSB1108049 COMPRESSION SPRING 3.5 X 19.7 X 70 97 PSB1108097 PULLEY
50 PSB1108050 COMPRESSION SPRING BUSHING BLOCK 98 PSB1108098 FENDER WASHER 5MM
51 PSB1108051 OUTFEED ROLLER 99 PSB1108099 OIL PLUG NPT 1/4 X 3/4
52 PSB1108052 SPROCKET SIZE 31T 100 PSB1108100 GEA R B OX
HAND W HEEL TYPE-11 150D X 10B- K X 3 / 8-16
74 PSB1108074 CAP SCREW M8-1.25 X 50
-58-
Page 64
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
PARTS
SB1108 Main Parts List (Cont.)
101 PSB1108101 GEA R 1 8 T 116 PSB1108116 ANTI-KICKB ACK FINGER
102 PSB1108102 KEY 4 X 4 X 16 RE 117 PSB1108117 SH A FT 19.95MM
103 PSB1108103 GEA RED SH AFT 18T/22T 118 PSB1108118 SPROCKET 31T
104 PSB1108104 GEA R 71T 119 PSB1108119 CHAIN #06B X 67P
105 PSB1108105 GEA RBOX GUA RD 202 PSB1108202 B ALL BEA RIN G 6003Z Z
106 PSB1108106 FLAT WASHER 6MM 203 PSB1108203 OIL SEAL 12 X 22 X 7
107 PSB1108107 TIMIN G B ELT 3GT-741-1 5 204 PSB1108204 CAP SCREW M5-.8 X 6
108 PSB1108108 GEARBOX COVER 205 PSB1108205 FLAT WASHER 5MM
109 PSB1108109 EXT RETAINING RIN G 12MM 207 PSB1108207 OUTER CHA IN TEN SIONER
110 PSB1108110 ADJUSTING SHAFT 208 PSB1108208
111 PSB1108111 LOC K ROD 212 PSB1108212 SET SCREW M6-1 X 16
112 PSB1108112 HEX NUT M12-1.75 220 PSB1108220 PHLP HD SCR M5-.8 X 8
113 PSB1108113 INFEED ROLLER 221 PSB1108221 C ORD ROUTIN G COVER
114 PSB1108114 E-CLIP 1 5MM 223 PSB1108223 CHIP B REAKER
115 PSB1108115 SPACER 20.5 X 32 X 6 224 PSB1108224 FOAM S TRIP 8 X 1 0 X 390
ST AN DO FF-H EX MM 5 /16- 18 X 2-1/ 2, 3-5 /16
-59-
Page 65
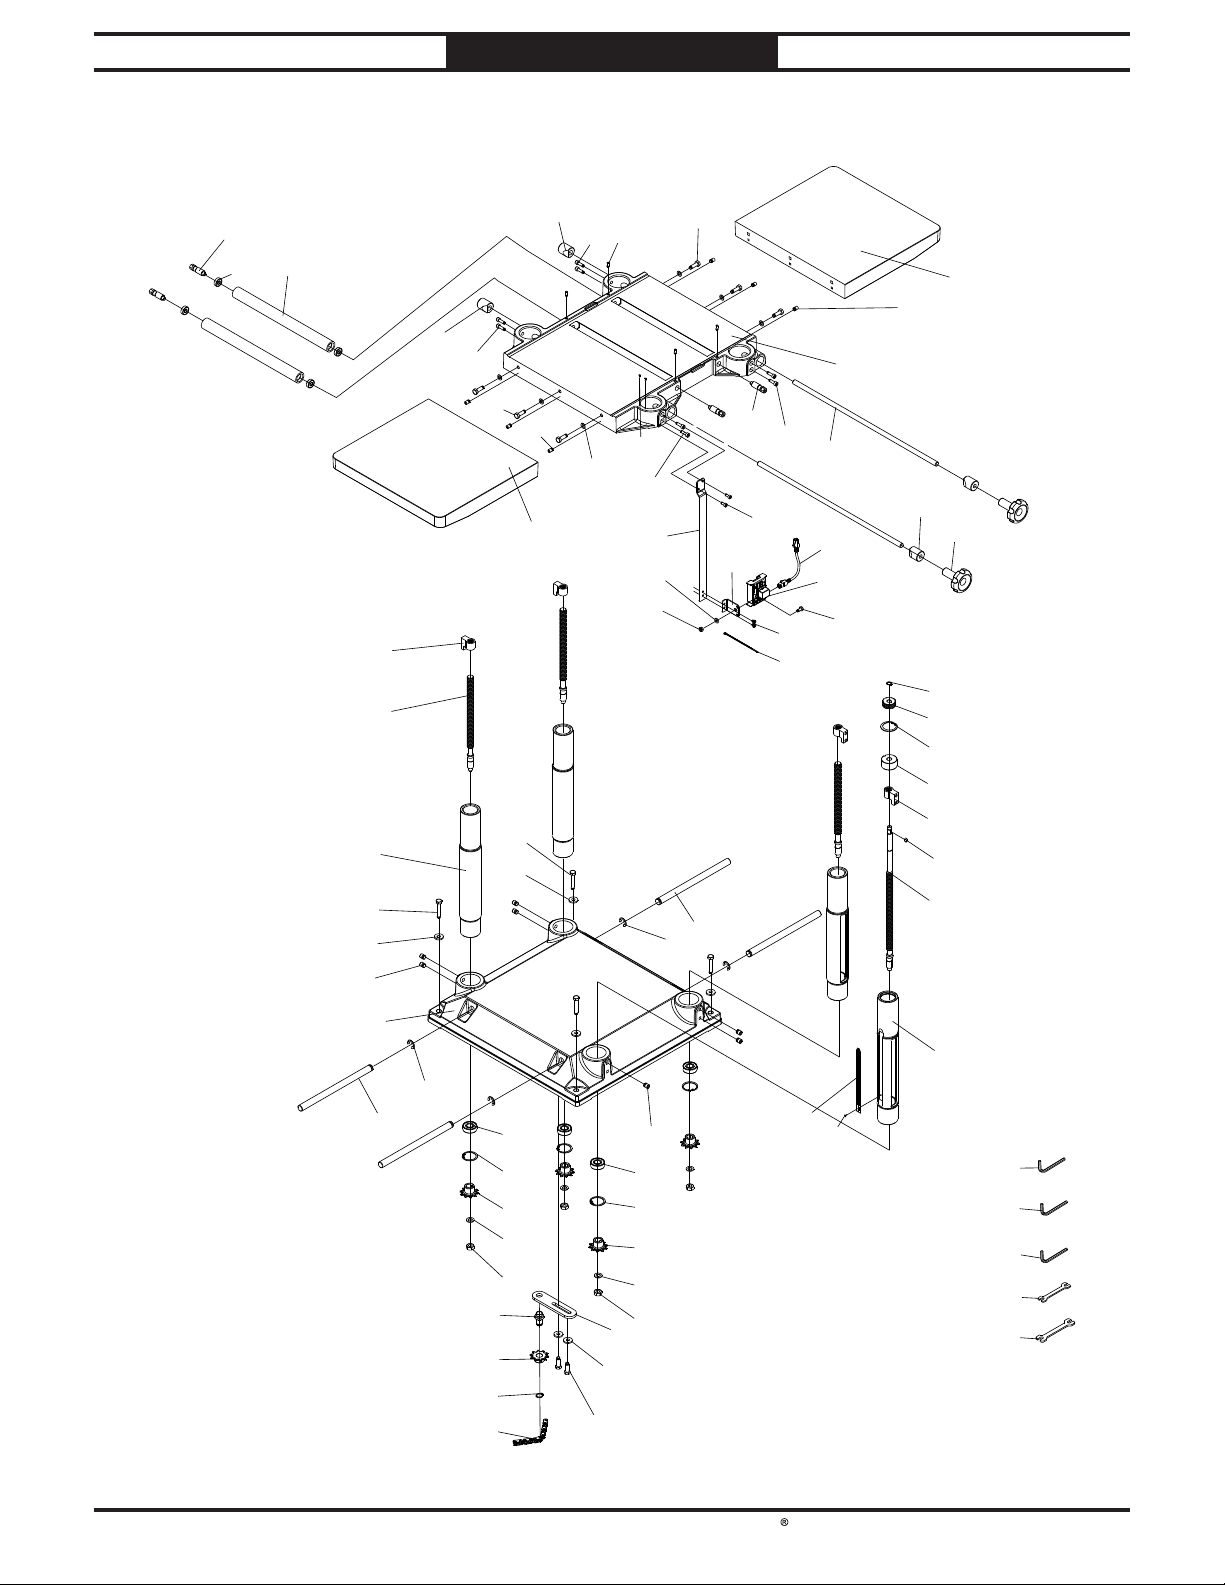
South Bend Tools
Model SB1108/ SB1109
PARTS
SB1108 Table & Base
For Machines Mfd. Since 12/20
120
19
121
139
142
143
144
43
122
16
127
144
43
128
129
122
16
225
42
215
16
68
106
71
146
127
147
70
120
93
16
216
222
123
229
228
129
128
126
124
125
35
135
136
137
138
139
22
140
-60-
36
145
146
153
154
155
156
148
149
150
151
30
43
127
152
36
148
149
150
151
30
141
131
157
181
182
183
184
185
Page 66
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PARTS
SB1108 Table & Base Parts List
REF PART # DE SCRIPTION REF PART # DE SCRIPTION
16 PSB1108016 CAP SCREW M6-1 X 20 140 PSB1108140 LEA DSCREW, PRIMA RY
19 PSB1108019 B ALL B EARING 608 Z 141 PSB1108141 COLUMN, PRIMARY
22 PSB1108022 KEY 4 X 4 X 1 0 RE 142 PSB1108142 LEADSCREW, SECONDARY
30 PSB1108030 HEX NUT M10-1.25 143 PSB1108143 COLUMN , SECON DA RY
35 PSB1108035 HEX BOLT M6-1 X 12 144 PSB1108144 HEX BOLT M8-1.25 X 45
36 PSB1108036 SET SCREW M10-1.5 X 12 1 45 PSB1108145 BASE
42 PSB1108042 S ET S CREW M 6-1 X 12 146 PSB1108146 E-CLIP 12MM
43 PSB1108043 F ENDER WASH ER 8MM 1 47 PSB1108147 LIFTING BAR
68 PSB1108068 BRACKET 148 PSB1108148 B ALL BEA RIN G 620 2Z
70 PSB1108070 PLA TE 149 PSB1108149 I NT RETAINING RIN G 35MM
71 PSB1108071 H EX NUT M 6-1 1 50 PSB1108150 IDLER SPROCKET 1 0T
93 PSB1108093 CAP SCREW M5-.8 X 12 151 PSB1108151 FEN DER WA SHER 10MM
106 PSB1108106 FLAT WASHER 6MM 1 52 PSB1108152 B RACKET
120 PSB1108120 ECCENTRIC SHAFT 153 PSB1108153 SHAFT
121 PSB1108121 TA B LE ROLLER 1 54 PSB1108154 SPROCKET 1 0T
122 PSB1108122 TH RE ADED GI B 155 PSB1108155 EXT RETA IN IN G RING 15MM
123 PSB1108123 LOCK IN G ROD 156 PSB1108156 CH AIN #410 X 134P
124 PSB1108124 GIB 157 PSB1108157 PHLP HD SCREW M3-.5 X 6
125 PSB1108125 KN OB LOB ED M12-1 . 75 181 PSB1108181 HEX WRENCH 6MM
126 PSB1108126 MAIN TABLE 182 PSB1108182 HEX WRENCH 4MM
127 PSB1108127 HEX BOLT M8-1.25 X 25 183 PSB1108183 HEX WRENCH 3MM
128 PSB1108128 SET SCREW M8 -1 X 12 184 PSB1108184 WRENCH 10 X 13MM OPEN-EN DS
129 PSB1108129 EXTEN SION TA BLE 185 PSB1108185 WRENCH 12 X 1 4MM OPEN -ENDS
131 PSB1108131 SCALE 215 PSB1108215 RIVET 2 X 5
135 PSB1108135 EXT RETAINING RING 10MM 216 PSB1108216 PHLP HD SCR M5-.8 X 6
136 PSB1108136 GEA R 14T 222 PSB1108222 CA BLE TIE 4"
137 PSB1108137 INT RETAI NI NG RING 38MM 225 PSB1108225 FLAT WASHER 8MM
138 PSB1108138 BUSHING 228 PSB1108228 DRO REMOTE S EN S OR
139 PSB1108139 LEADSCREW N UT 1 6-4 229 PSB1108229 DRO CORD CAT5E 39"
-61-
Page 67
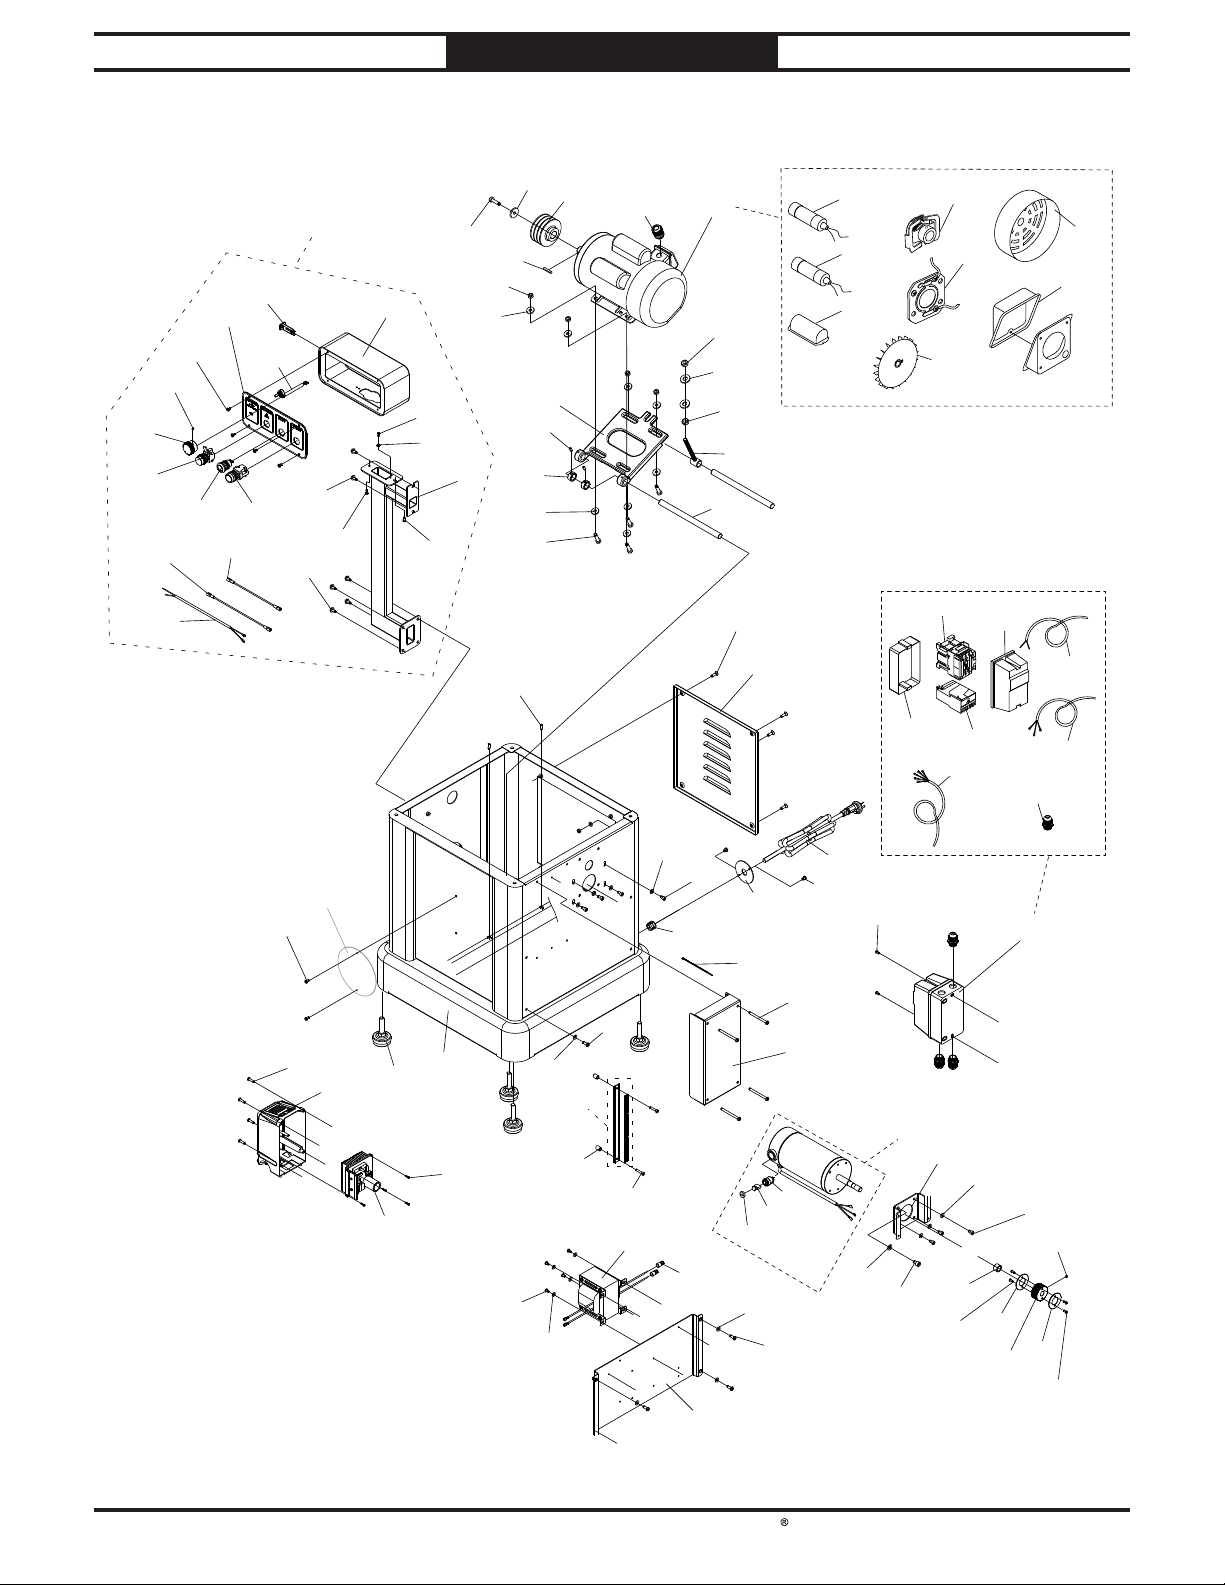
South Bend Tools
Model SB1108/ SB1109
PARTS
SB1108 Stand & Motor
234
233
159-11
159-12
159-13
159-17
159-9
159-10
159-14
159-7
159-8
159-15
159-16
159
159-1
159-6
159-5
159-6
159-2
159-3
159-4
159-5
232
231
163
43
164
42
210
43
162
235
134
30
165
30
166
167
For Machines Mfd. Since 12/20
134-1
134-2
134-3
134-4
134-5
134-6
134-7
134-8
159-18
213
179
306
180
161
186
160
65
212
106
227
217
66
218
256
106
171
77
169
222
168
263
172-2
172-3
219
206
172-1
170
259
198
158-3
158-2
172
158-4
158-5
173
158-1
158-6
158-7
158-8
158
106
77
200
-62-
201
178
257
209
106
66
11
174
175
95
176
177
176
95
Page 68
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PARTS
SB1108 Stand & Motor Parts List
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
11 PSB1108011 FLAT WASHER 8MM 161 PSB1108161 FOOT M1 2-1.75
30 PSB1108030 HEX NUT M10-1.25 162 PSB1108162 HEX BOLT M8-1.25 X 30
42 PSB1108042 S ET SCREW M6-1 X 12 163 PSB1108163 H EX NUT M8-1.2 5
43 PSB1108043 F ENDER WASH ER 8MM 164 PSB1108164 MOTOR MOUNT PLATE
65 PSB1108065 TAP S CREW M3 X 8 165 PSB1108165 FEN DER WASHER 10MM
66 PSB1108066 PHLP HD SCR M6-1 X 16 166 PSB1108166 MOTOR MOUN T CONNECTIN G ROD
77 PSB1108077 CAP SCREW M6-1 X 12 167 PSB1108167 SHAFT
95 PSB1108095 PHLP HD SCR M4-.7 X 10 168 PSB1108168 M OTOR A CCES S PA N EL
106 PSB1108106 FLAT WASHER 6MM 169 PSB1108169 PHLP HD SCR M6-1 X 20
134 PSB1108134 M OTOR 3HP 230V 1 -P H 1 70 PSB1108170 PHLP HD SCR M6-1 X 10
134-1 PSB1108134-1 S CAPACITOR 400M 125V 1-9/16 X 3-9/16 171 PSB1108171 STRAIN RELIEF TYPE-1 19MM
134-2 PSB1108134-2 R CAPACITOR 70M 250V 1-9/16 X 3-9/1 6 172 PSB1108172 DC MOTOR 3/4HP 90VDC 8 A
134-3 PSB1108134-3 CAPACITOR COVER 1 72-1 PSB1108172-1 BRUSH B RACKET
134-4 PSB1108134-4 CEN T SWITCH 16 MM 3450 172-2 PSB1108172-2 MOTOR BRUS H 120V (2-PC SET)
134-5 PSB1108134-5 CONTACT PLATE 16MM 1 72-3 PSB1108172-3 BRUSH COVER
134-6 PSB1108134-6 MOTOR FA N 173 PSB1108173 MOTOR MOUNT PLATE
134-7 PSB1108134-7 MOTOR F AN COVER 174 PSB1108174 CAP SCREW M8-1.25 X 12
134-8 PSB1108134-8 MOTOR JUNCTION B OX 175 PSB1108175 COLLAR
158 PSB1108158 MAGNETIC SWITCH SDE MPE-18 176 PSB1108176 PULLEY COVER
158-1 PSB1108158-1 MAG SWITCH COVER 177 PSB1108177 PULLEY
158-2 PSB1108158-2 MAG SWITCH BASE 178 PSB1108178 FLAT WASHER 5MM
158-3 PSB1108158-3 CONTACTOR SDE MA-16 220V 179 PSB1108179 PHLP HD SCR M5-.8 X 20
158-4 PSB1108158-4 OL RELAY SDE RA-20 12-18A 180 PSB1108180 DC MOTOR CONTROL COVER
158-5 PSB1108158-5 CONTROL P ANEL CORD 18G 5W 86" 186 PSB1108186 DC MOTOR CONTROLLER AC 120V/DC
158-6 PSB1108158-6 TRANSF ORMER CORD 18G 2W 23" 198 PSB1108198 PHLP HD SCR 3/16-24 X 3/8
158-7 PSB1108158-7 MOTOR CORD 1 2G 3W 33" 200 PSB1108200 SET SCREW M5-.8 X 5
158-8 PSB1108158-8 STRAIN RELIEF TYPE-3 PG13.5 201 PSB1108201 PHLP HD SCR M5-.8 X 10
159 PSB1108159 CONTROL PAN EL ASS EMBLY 206 PSB1108206 DRO SENSOR COVER
159-1 PSB1108159-1 CON TROL PA N EL B OX 209 PSB1108209 SWITCH PANEL
159-2 PSB1108159-2 PHLP HD SCR M4-.7 X 6 210 PSB1108210 SPACER 16.2 X 25 X 12.7
159-3 PSB1108159-3 EXT TOOTH WASH ER 4MM 212 PSB1108212 SET SCREW M6-1 X 16
159-4 PSB1108159-4 CON TROL PANEL PEDESTAL 213 PSB1108213 PHLP HD SCR M5-.8 X 10
159-5 PSB1108159-5 HEX BOLT M5-.8 X 10 217 PSB1108217 SPACER 7 X 11.9 X 13.5
159-6 PSB1108159-6 F LANGE B OLT M6-1 X 12 218 PSB1108218 CAP SCREW M5-.8 X 25
159-7 PSB1108159-7 CIRCUIT B REA KER S WITCH 10A ZE-80 0 219 PSB1108219 PHLP HD SCR M6-1 X 70
159-8 PSB1108159-8 POTENTIOMETER 50K X 1900MM 222 PSB1108222 CABLE TIE 4"
159-9 PSB1108159-9 CONTROL PANEL FACE PLATE 227 PSB1108227 DRO SEN SOR STRIP
159-10 PSB1108159-10 PHLP HD SCR M5-.8 X 8 231 PSB1108231 KEY 5 X 5 X 30 RE
159-11 PSB1108159-11 S ET S CREW M 4-.7 X 6 232 PSB1108232 HEX BOLT M8-1.25 X 25
159-12 PSB1108159-12 FEED SPEED ADJUSTMENT KNOB 233 PSB1108233 MOTOR PULLEY
159-13 PSB1108159-13
159-14 PSB1108159-14 E-STOP BUTTON RENY 250 V, 22MM 235 PSB1108235 S TRAIN RELIEF TYPE-3 PG13.5
159-15 PSB1108159-15 START SWITCH YUAN GUAN 250 V, 22MM 256 PSB1108256 TRANSF ORMER SUEN SPCL2 0660 220V
159-16 PSB1108159-16 S TOP B UTTON CORD 18G 1W 6" 257 PSB1108257 WIRE NUT P3
159-17 PSB1108159-17 DC CONTROLLER CORD 18G 1W 8" 259 PSB1108259 POWER CORD 12G 3W 138" 6-20P
159-18 PSB1108159-18 CIRCUIT B REAKER CORD 18 G 2W 71" 263 PSB1108263 PLA TE
160 PSB1108160 CABINET STAND
POWER INDICATOR LIGHT YUAN GUAN 25MM
234 PSB1108234 FENDER WASHER 8MM
-63-
Page 69
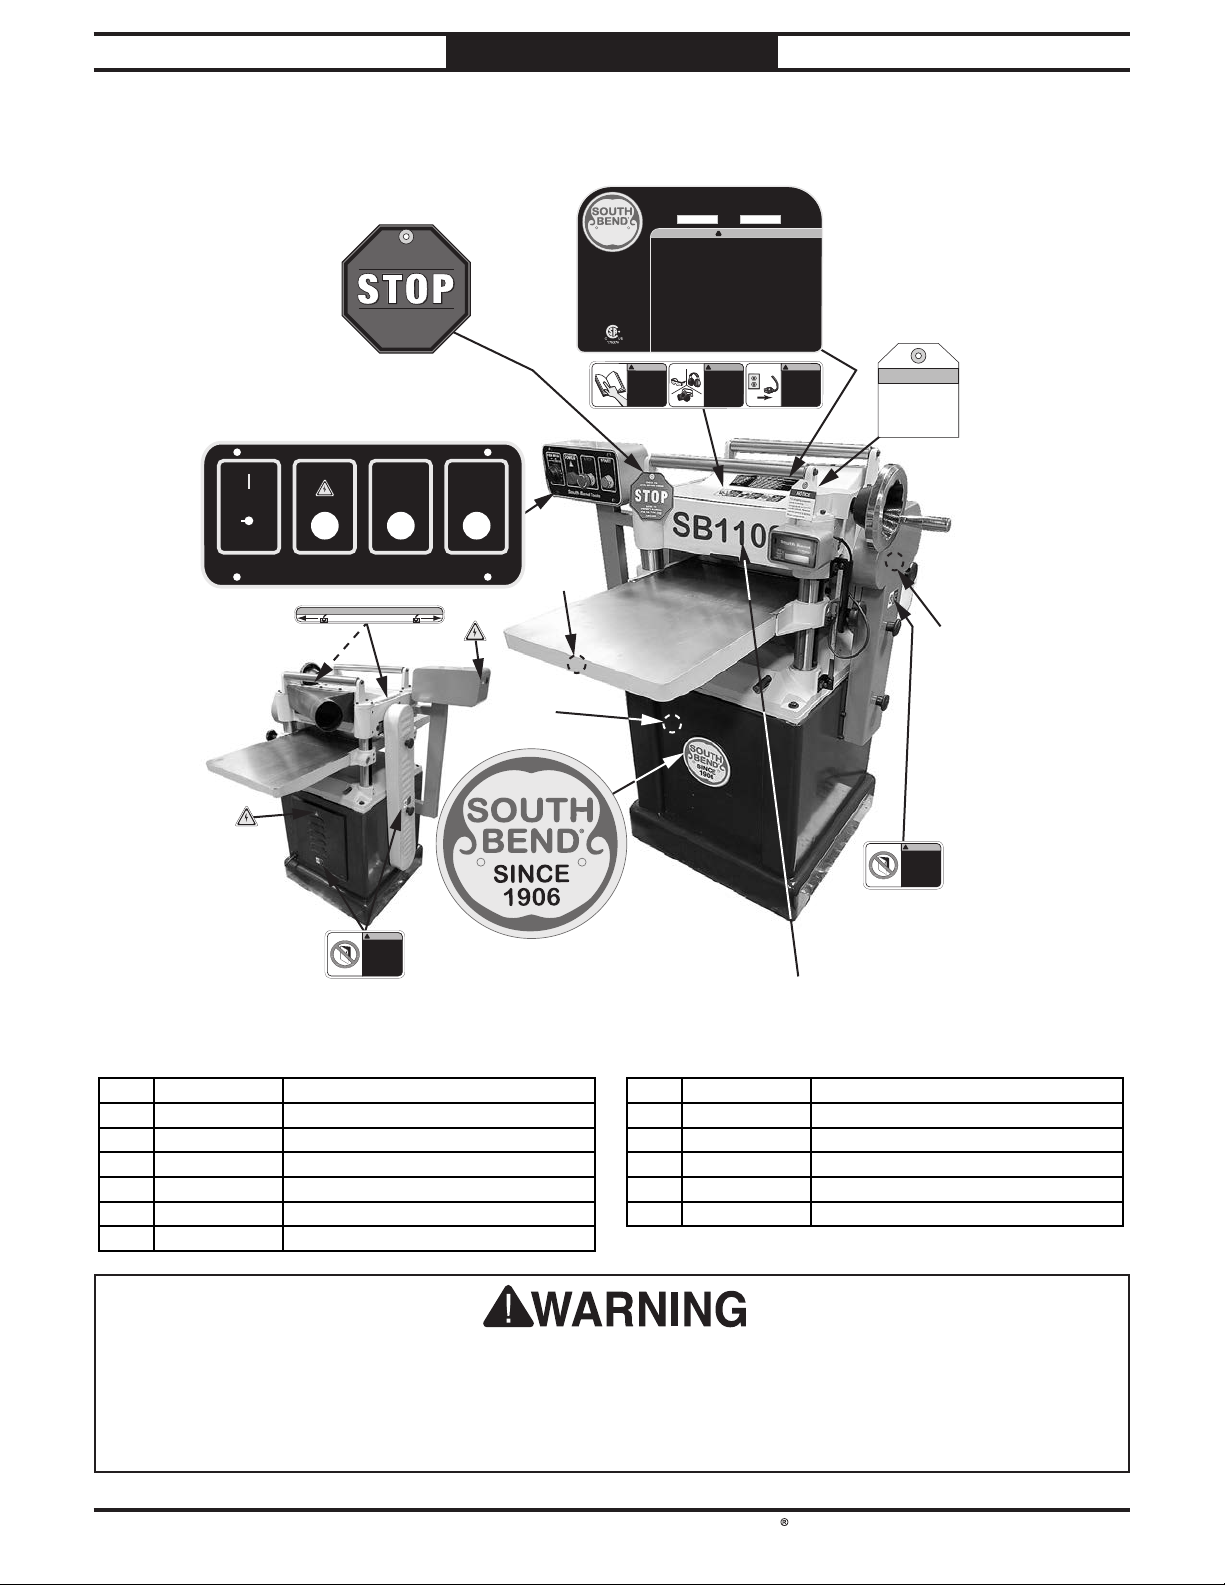
South Bend Tools
Model SB1108/ SB1109
SB1108
PARTS
SB1108 Labels & Cosmetics
MODEL SB1108
15" Planer w/Helical Cutterhead
FEED SPEED
– +
28 FPM
10 FPM
312
POWER
LEVEL BEFORE USING!
OWNER’S MANUAL
FOR OIL TYPE AND
311
CHECK OIL
REFER TO
AMOUNT.
STOP
300
START
SINCE
1906
Main Motor: 3 HP, 230V, 1-Ph, 60 Hz
Full-Load Current Rating: 12A
Cutterhead: 4 Spirals, 52 Inserts
Replacement Inserts: H9893
Cutterhead Speed: 5000 RPM
Feed Rates: 10–28 FPM
Max. Depth of Cut: 1/8"
Min. Stock Thickness: 3/16"
Min. Stock Length: 6"
Max. Cutting Width: 15"
Max. Cutting Height: 6"
Weight: 509 lbs.
Made in Taiwan to South Bend Specications
service, or adjustments.
!
!
WARNING!
INJURY HAZARD
To reduce risk of
short- and
long-term injury,
wear eye, ear, and
lung protection
when using this
To reduce the risk of serious injury when using this machine:
1. Read and understand owner’s manual before operating.
2. Always wear approved safety glasses, hearing protection, and respirator.
3. Disconnect power before changing blades, removing parts, or doing maintenance,
4. Only plug power cord into a grounded outlet.
5. Do not wear loose clothing, gloves, jewelry, or other items that
can get entangled. Tie back long hair and roll up sleeves.
6. Ensure machine is correctly set up before starting.
7. Do not plane two boards of varying thickness at the same time.
8. Never plane material smaller than 6" long, 3/4” wide, or 3/16" thick.
9. Do not allow hands or clothing to get pulled into cutting area while feeding workpiece.
10. Stand clear of board ends during cutting operation.
11. Do not plane boards with cracks, loose knots, or other defects.
12. Inserts are sharp! Use extreme caution when changing/adjusting.
13. Never reach into cutting area while machine is running.
14. Keep ngers clear of pinch point bet ween stock and table.
15. Do not operate when tired or under inuence of drugs or alcohol.
16. Do not expose to rain or use in wet locations.
17. Prevent unauthorized use by children or untrained users;
restrict access or disable machine when unattended.
!
WARNING!
INJURY HAZARD
Do not use machine
if you have not read
the manual. Visit
southbendtools.com
or call 360-734-1540
to get a manual.
301
WARNING!
For Machines Mfd. Since 12/20
MFG DateSerial No
302
!
WARNING!
INJURY/SHOCK
HAZARD
!
To avoid shock or
accidental starting,
disconnect power
before adjusting or
servicing machine.
NOTICE
For shipping purposes,
some inventory
components are packed
inside cabinet. Remove
cabinet panels to access
these components.
South Bend Tools
310
NOTICE
Add SAE 30 oil every 24 hours of operation.
307
309
303
308
307
!
WARNING!
INJURY HAZARD
Keep cover closed
while machine is
operating.
Disconnect power
before removing or
servicing.
306
305
304
!
WARNING!
INJURY HAZARD
Keep cover closed
while machine is
operating.
Disconnect power
before removing or
servicing.
304
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
300 PSB1108300 MACHINE ID LABEL 307 PSB1108307 ELECTRICITY LAB EL 0.7
301 PSB1108301 COM B O WA RN IN G LAB EL 308 PSB1108308 TOUCH -UP PAINT, SB LIGHT BLUE
302 PSB1108302 INVENTORY SHIPPING NOTICE 30 9 PSB1108309 TOUCH-UP PAIN T, SB GRAY
303 PSB1108303 TOUCH-UP PAIN T, S B DARK B LUE 310 PSB1108310 ADD OIL NOTICE
304 PSB1108304 DOOR CLOSED LABEL 2.5 X 1.5 311 PSB1108311 CONTROL PANEL LA BEL
305 PSB1108305 MODEL NUMBER LAB EL 31 2 PSB1108312 STOP OIL FILL TA G
306 PSB1108306 SOUTH BEN D NAMEPLATE 6"
The safety labels provided with your machine are used to make the operator aware of the
machine hazards and ways to prevent injury. The owner of this machine MUST maintain the
original location and readability of these safety labels. If any label is removed or becomes
unreadable, REPLACE that label before using the machine again. Contact South Bend Tools at
(360) 734-1540 or www.southbendtools.com to order new labels.
-64-
Page 70
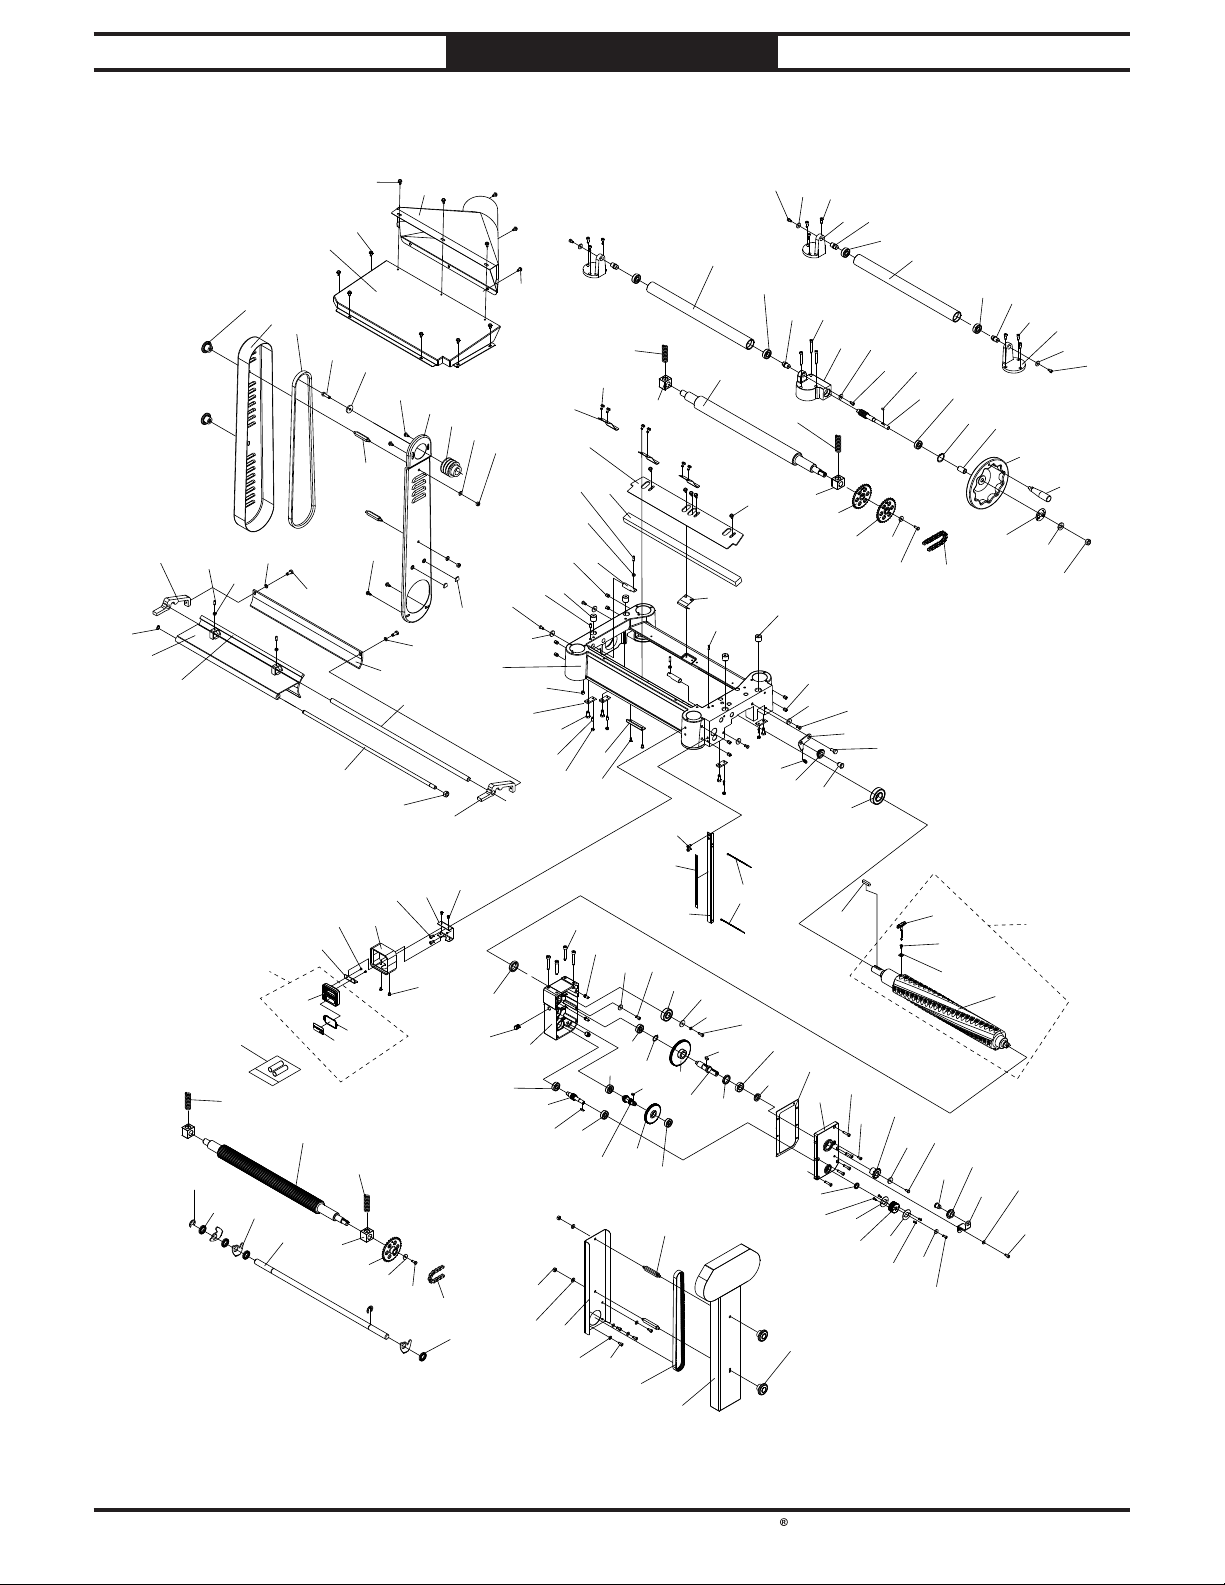
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PARTS
SB1109 Main
116
117
112
119
40
113
21
56
41
40
20
8
66
15
54
39
67
19
55
16
57
38
43
68
22
17
23
58
69
18
64
42
16
59
19
20
15
60
65
21
24
25
61
26
27
20
212
28
19
29
17
231
31
18
16
249
15
8
13
8
14
11
45
12
42
43
47
8
40
46
76
39
48
32
38
77
35
36
54
8
55
33
34
37
49
50
232
1
2
3
4
6
8
9
10
7
118
8
44
5
114
115
31
112
5
48
121
122
71
54
53
123
53-1
124
120
75
99
53-3
54
55
125
52
53-2
15
59
60
51
237
126
237
122
78
104
86
105
106
107
12
11
110
79
86
111
80
86
108
81
59
86
109
127
87
88
72
238
81
86
225
128
82
89
90
83
84
91
239
92
85
222
93
223
100
1
94
95
63
101
96
102
97
101
100
98
59
103
62-1
42
68
97
62-2
62-3
67
135
62
62-4
111
81
-65-
Page 71
South Bend Tools
Model SB1108/ SB1109
PARTS
For Machines Mfd. Since 12/20
SB1109 Main Parts List
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
1 PSB1109001 KNOB 5/16 -1 8 LOB ED 53 PSB1109053 DIGITAL READOUT AS SEMB LY
2 PSB1109002 B ELT PULLEY COVER 53-1 PSB1109053-1 DIGITAL READOUT WIXEY MODEL WR5502
3 PSB1109003 V-B ELT M 58 53-2 PSB1109053-2 BATTERY COVER
4 PSB1109004 HEX BOLT M8-1.25 X 30 53-3 PSB1109053-3 BATTERY COVER DECAL
5 PSB1109005 LOCK WASHER 8MM 54 PSB1109054 COMPRESSION SPRING 3.5 X 19.7 X 70
6 PSB1109006 FENDER WASHER 8MM 55 PSB1109055 COMPRESSION SPRING BUSHING BLOCK
7 PSB1109007 STANDOFF-HEX MM 5/16-18 X 2-1 /4, 3/8 56 PSB1109056 OUTFEED ROLLER
8 PSB1109008 FLANGE B OLT M6-1 X 12 57 PSB1109057 SPROCKET 31T
9 PSB1109009 BELT PULLEY GUARD 58 PSB1109058 SPROCKET 31T
10 PSB1109010 PULLEY 59 PSB1109059 FENDER WASHER 6MM
11 PSB1109011 FLAT WASHER 8MM 60 PSB1109060 HEX BOLT M6-1 X 16
12 PSB1109012 HEX NUT 5/16-18 61 PSB1109061 CH AIN #06B X 44P
13 PSB1109013 DUST HOOD W/5" PORT 62 PSB1109062 HELICAL CUTTERHEAD ASSY
14 PSB1109014 UPPER COVER 62-1 PSB1109062-1 T-HAN DLE TORX DRIVER T25
15 PSB1109015 CAP SCREW M6-1 X 10 62-2 PSB1109062-2 F LAT HD TORX 10 -32 X 1/2
16 PSB1109016 FENDER WASHER 6MM 62-3 PSB1109062-3 INSERT 15 X 15 X 2.5MM-10 PK
17 PSB1109017 CAP SCREW M6-1 X 16 62-4 PSB1109062-4 HELICA L CUTTERH EAD 20"
18 PSB1109018 RETURN ROLLER BRACKET 63 PSB1109063 KEY 8 X 8 X 36 RE
19 PSB1109019 BEARING SHAFT 64 PSB1109064 CHAIN TENSIONER
20 PSB1109020 BALL BEARING 6202-2NSE 65 PSB1109065 SHOULDER BOLT M8-1.25 X 14.5, 4 X 12
21 PSB1109021 RETURN ROLLER 66 PSB1109066 EXTENSION SPRING 1 X 8.5 X 35
22 PSB1109022 CAP SCREW M6-1 X 50 67 PSB1109067 IDLER WHEEL
23 PSB1109023 WORM GEAR HOUSIN G 68 PSB1109068 IDLER SHAFT
24 PSB1109024 KEY 4 X 4 X 10 RE 69 PSB1109069 BALL B EARING 6206-2NS E
25 PSB1109025 WORM SHAFT 71 PSB1109071 BATTERY AAA (2 PCS)
26 PSB1109026 BALL BEARIN G 6201Z 72 PSB1109072 SCALE
27 PSB1109027 IN T RETAINING RING 32MM 75 PSB1109075 MOUNTING PLA TE
28 PSB1109028 COLLAR 76 PSB1109076 SET SCREW M1 0-1.5 X 30
29 PSB1109029 HANDWHEEL TYPE-14 200D 12B-K 3/8-16 77 PSB1109077 HEX NUT M10-1.5
31 PSB1109031 HEX NUT M12-1.75 78 PSB1109078 OIL S EAL 28 X 40 X 8
32 PSB1108032 SPRING PLA TE 79 PSB1109079 CAP SCREW M8-1.25 X 50
33 PSB1109033 CHIP DEFLECTOR 80 PSB1109080 ROLL PIN 8 X 20
34 PSB1109034 FOAM GASKET 81 PSB1109081 CAP SCREW M6-1 X 12
35 PSB1109035 SET SCREW M6-1 X 20 82 PSB1109082 BALL BEA RIN G 6204-2NS E
36 PSB1109036 HEX NUT M6-1 83 PSB1109083 FENDER WASHER 6MM
37 PSB1109037 SHAFT 5/8 84 PSB1109084 LOCK WASHER 6MM
38 PSB1109038 SET SCREW M10-1.5 X 12 85 PSB1109085 CAP SCREW M6-1 X 16
39 PSB1109039 OILER SCREW M22-1.5 X 20 86 PSB1109086 BA LL BEARING 6201ZZ
40 PSB1109040 SET SCREW M6-1 X 16 87 PSB1109087 EXT RETA IN IN G RING 20MM
41 PSB1109041 SPRING PLATE 88 PSB1109088 KEY 5 X 5 X 10 RE
42 PSB1109042 HEX BOLT M6-1 X 12 89 PSB1109089 GEA R 96T
43 PSB1109043 FENDER WASHER 6MM 90 PS B 1 109090 SHAFT 24.5 X 10⁵
44 PSB1109044 PLATE 91 PS B 1 109091 OIL S EAL 25 X 35 X 5
45 PSB1109045 HEAD CASTING 92 PS B 11090 92 KEY 6 X 6 X 15 RE
46 PSB1109046 SET S CREW M8-1.25 X 12 93 P SB110 90 93 COLLAR
47 PSB1109047 PLATE 94 PSB11 0 90 94 GAS KET
48 PSB1109048 HEX BOLT M8-1.25 X 20 95 PS B 1 109095 GEA RB OX COVER
49 PSB1109049 DEPTH LIMITER 96 PSB11 0 90 96 CAP SCREW M6-1 X 25
50 PSB1109050 FLA T HD SCR M5-.8 X 12 97 PSB11 0 90 97 CAP SCREW M5-.8 X 12
51 PSB1109051 DIGITAL REA DOUT BRACKET 98 P S B 11090 98 SPROCKET 12T
52 PSB1109052 DIGITA L READOUT HOUSING 99 P SB110 90 99 TAP SCREW M3 X 8
-66-
Page 72
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
PARTS
SB1109 Main Parts List (Cont.)
ST AN DO FF-H EX MM 5 /16- 18 X 2-1/ 2, 3-5 /16
-67-
Page 73
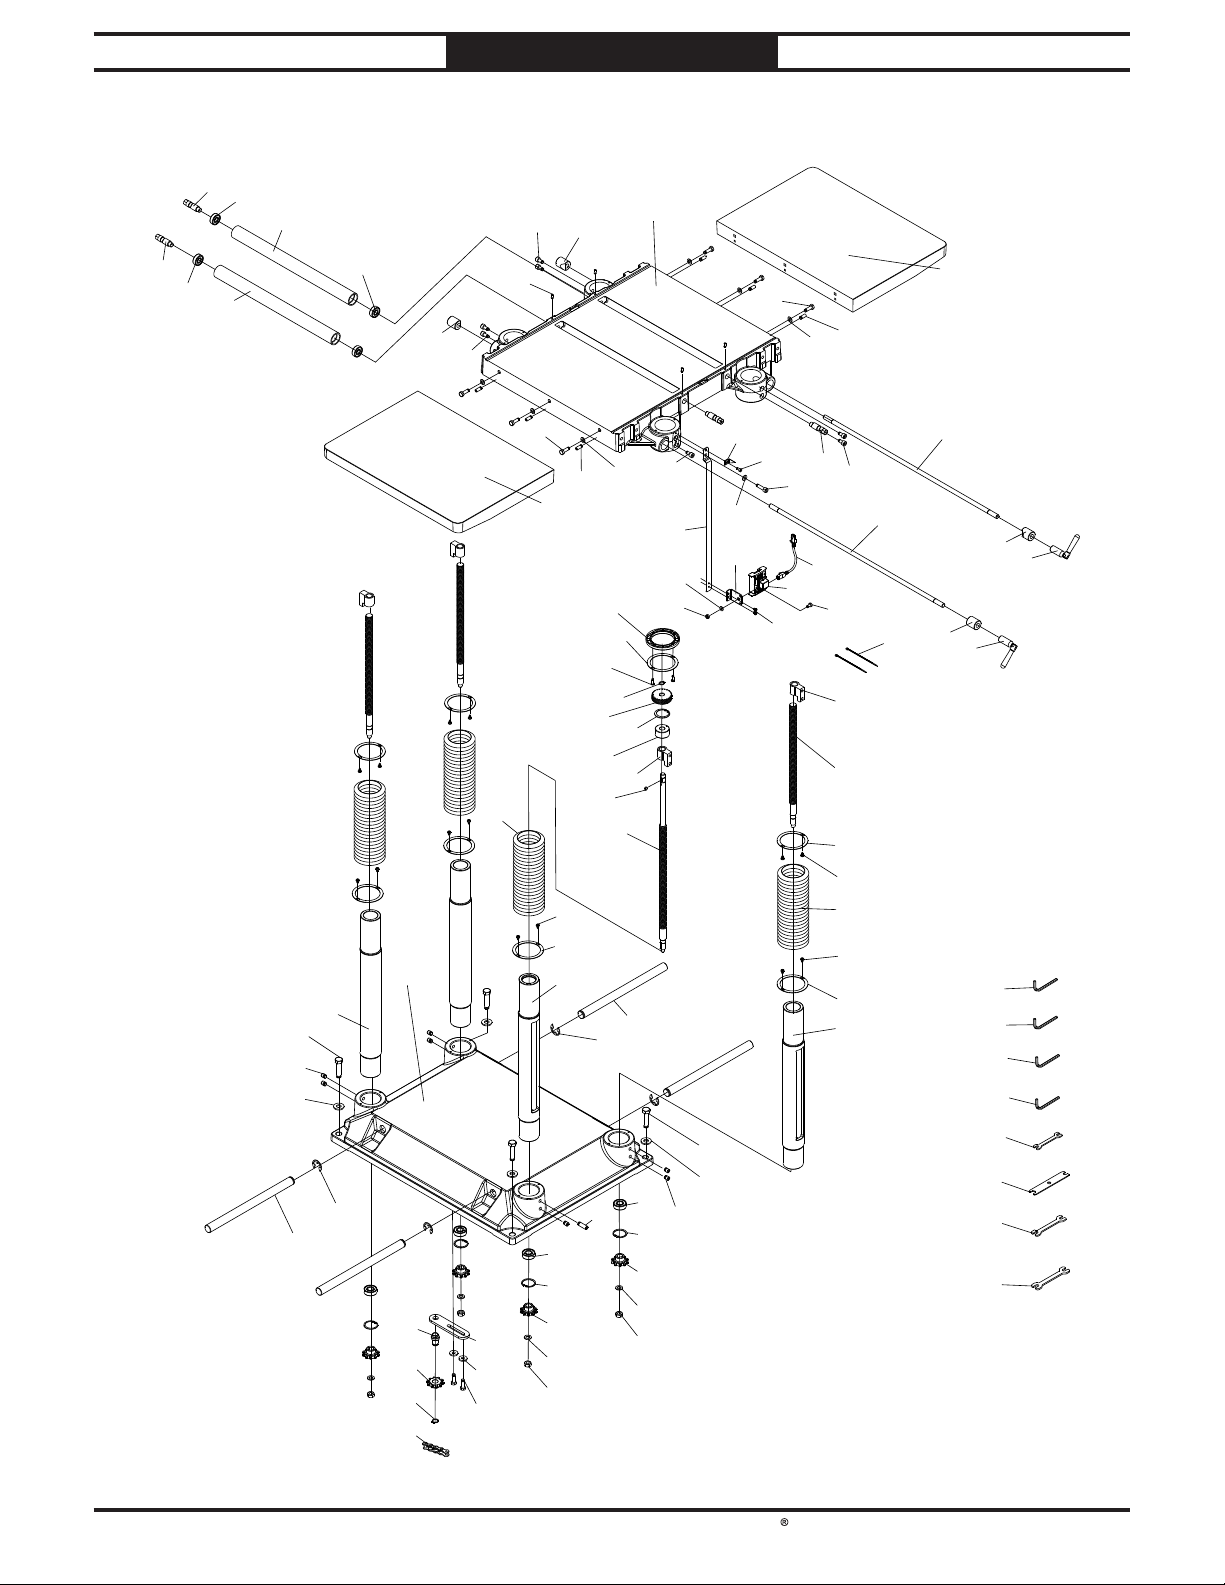
South Bend Tools
Model SB1108/ SB1109
PARTS
SB1109 Table & Base
129
26
130
131
For Machines Mfd. Since 12/20
134
132
129
26
130
26
132
131
133
153
136
137
46
146
149
144
147
24
240
145
116
148
150
152
131
74
111
113
141
11
189
136
142
143
243
230
240
129
244
42
157
46
131
150
145
138
239
137
138
139
140
139
140
160
38
161
162
158
163
159
171
172
173
174
169
170
136
154
145
156
164
165
166
167
168
76
163
162
164
165
166
167
168
38
160
161
154
153
154
145
158
203
204
205
206
207
208
209
210
-68-
Page 74
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PARTS
SB1109 Table & Base Parts List
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
11 PSB1109011 FLAT WASHER 8MM 154 PSB1109154 PHLP HD SCR M5-2.12 X 10
24 PSB1109024 KEY 4 X 4 X 10 RE 156 PSB1109156 COLUMN, PRIMARY
26 PSB1109026 BALL BEARIN G 6201Z 157 PSB1109157 LEADSCREW, SECONDARY
38 PSB1109038 SET SCREW M10-1.5 X 12 158 PSB1109158 COLUM N, S ECONDARY
42 PSB1109042 HEX BOLT M6-1 X 12 159 PSB1109159 BASE
46 PSB1109046 SET S CREW M8-1.25 X 12 160 PSB1109160 HEX B OLT M12-1.75 X 50
74 PSB1109074 B RACKET 161 PSB1109161 FENDER WASHER 12MM
76 PSB1109076 SET SCREW M10-1 .5 X 30 162 PSB1109162 LIFTING BAR
111 PSB1109111 FLAT WASHER 6MM 163 PSB1109163 E-C LIP 17MM
113 PSB1109113 LOCK N UT M 6-1 164 PSB1109164 BALL B EARING 620 2Z
116 PSB1109116 EXT RETAINING RING 12MM 165 PSB1109165 IN T RETA IN IN G RING 35MM
129 PSB1109129 ECCENTRIC SHAFT 166 PSB1109166 S PROCKET 10 T
130 PSB1109130 TABLE ROLLER 167 PSB1109167 FLAT WASHER 10MM
131 PSB1109131 CAP SCREW M8-1.25 X 16 168 PSB1109168 HEX NUT M10-1.25
132 PSB1109132 THREA DED GIB 169 PSB1109169 BRACKET
133 PSB1109133 SET SCREW M6-1 X 12 170 PSB1109170 FENDER WASHER 8MM
134 PSB1109134 MAIN TABLE 171 PSB1109171 SHAFT
136 PSB1109136 HEX BOLT M8-1.25 X 25 172 PSB1109172 SPROCKET 1 0T
137 PSB1109137 EXTENS ION TAB LE 1 73 PSB1109173 EXT RETAINING RIN G 15MM
138 PSB1109138 LOCKING ROD 174 PSB1109174 CHAIN #40 X 166P
139 PSB1109139 THREA DED GIB 189 PSB1109189 PLATE
140 PSB1109140 PIVOT HANDLE M12-1.75 203 PSB1109203 HEX WRENCH 3MM
141 PSB1109141 SCA LE POINTER 204 PSB1109204 HEX WRENCH 4MM
142 PSB1109142 CAP SCREW M5-.8 X 10 205 PSB1109205 HEX WRENCH 5MM
143 PSB1109143 CAP SCREW M8-1.25 X 30 206 PSB1109206 HEX WRENCH 6MM
144 PSB1109144 PLATE 207 PSB1109207 WRENCH 8 X 10MM OPEN-ENDS
145 PSB1109145 COLLAR 208 PSB1109208 WRENCH 10 X 13MM OPEN-ENDS
146 PSB1109146 PHLP HD SCR M5-.8 X 15 209 PSB1109209 WRENCH 12 X 14MM OPEN-ENDS
147 PSB1109147 GEAR 24T 210 PSB1109210 WRENCH 17 X 19MM OPEN-ENDS
148 PSB1109148 INT RETAIN ING RING 38MM 230 PSB1109230 PHLP HD SCR M5-.8 X 6
149 PSB1109149 BUSHING 239 PSB1109239 CABLE TIE 4"
150 PSB1109150 LEADSCREW NUT 16 -4 240 PSB1109240 FLAT WASHER 8MM
152 PSB1109152 LEA DSCREW, PRIMARY 243 PSB1109243 DRO REMOTE SEN SOR
153 PSB1109153 DUST B OOT 244 PSB1109244 DRO CORD CAT5E 39"
-69-
Page 75
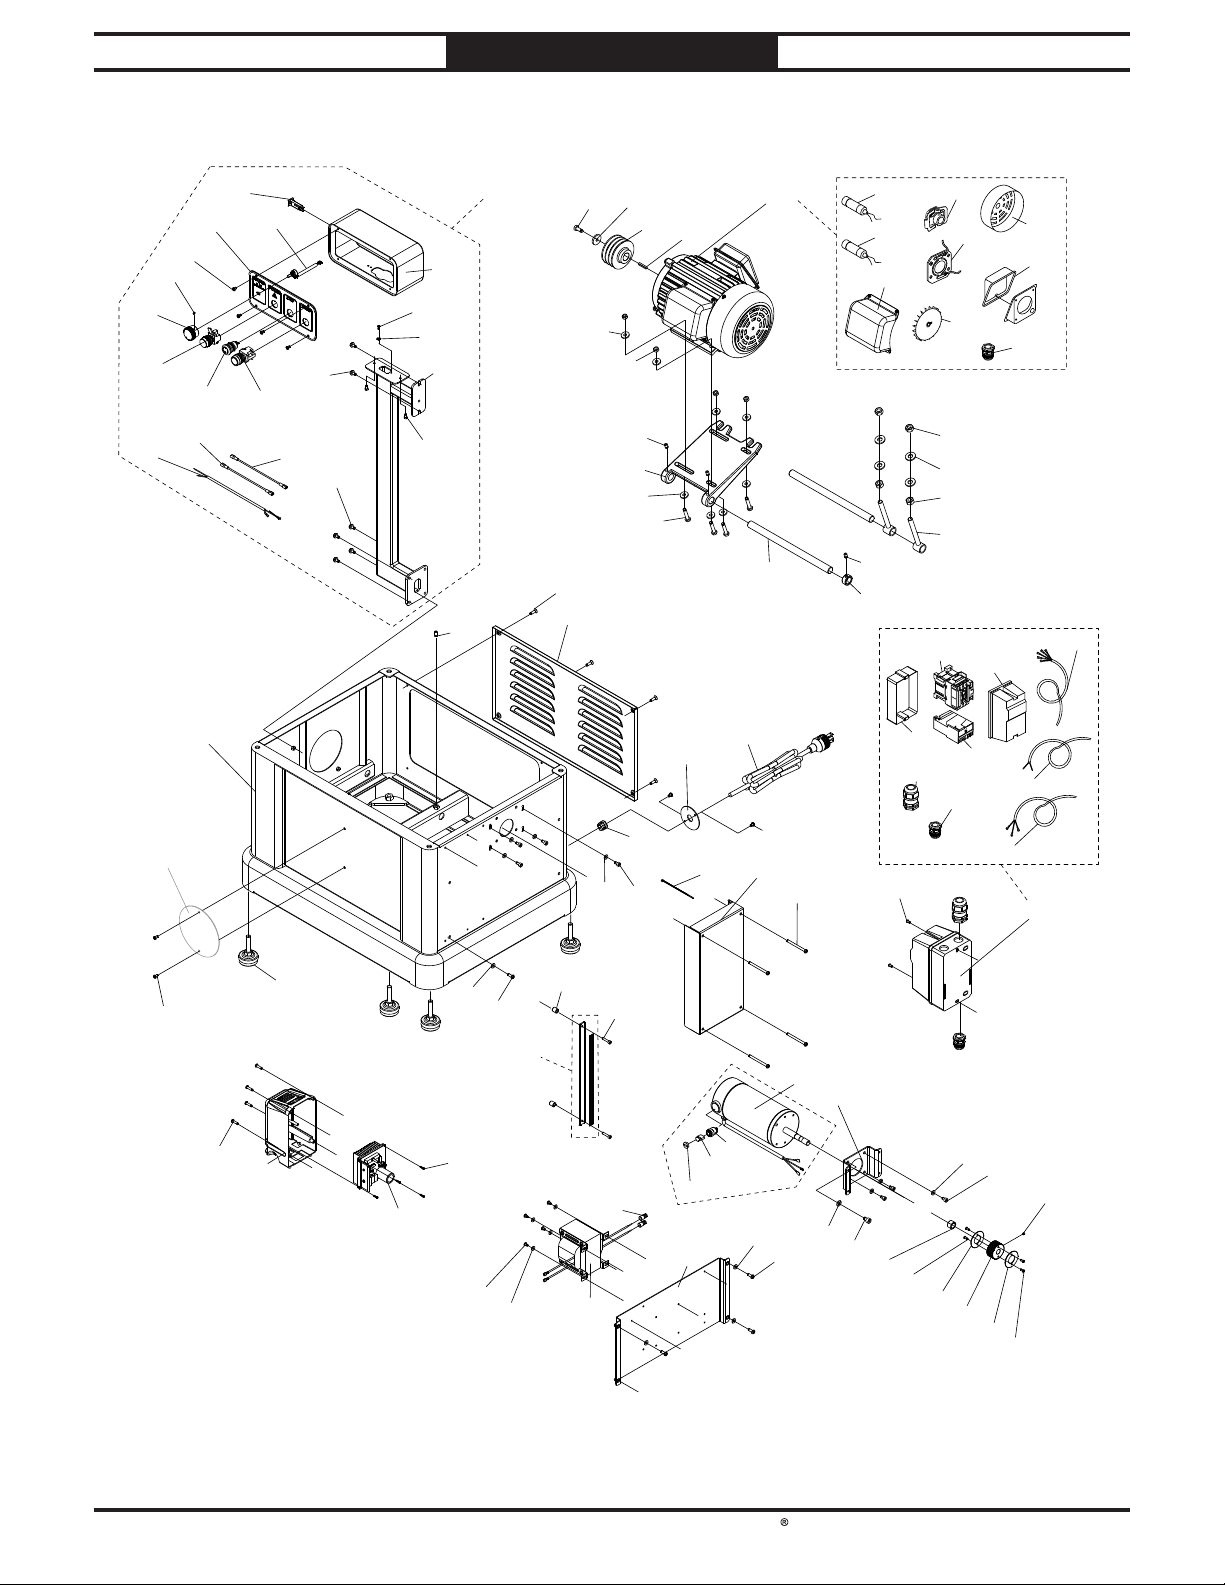
South Bend Tools
Model SB1108/ SB1109
PARTS
SB1109 Stand & Motor
For Machines Mfd. Since 12/20
176-11
176-12
176-13
176-18
176-9
176-10
176-14
176-17
177
176-7
176-8
176-6
176-15
176-16
176-6
176-1
176-2
176-3
176-4
176-5
179
176
181
248
170
180
247
184
46
182
170
183
246
245
220
251
175
185
46
186
175-1
175-2
175-3
188-2
175-4
188-3
188-5
188-6
175-5
175-6
31
30
31
187
188-1
188-4
175-7
175-8
175-9
188-7
188-8
310
228
202
201
178
252
111
99
199
70
200
242
233
254
253
111
234
190
15
191-3
226
239
191-1
191-2
235
111
73
236
70
191
192
193
194
195
227
100
188-9
188
111
81
221
196
197
196
100
-70-
Page 76
South Bend Tools
For Machines Mfd. Since 12/20 Model SB1108/ SB1109
PARTS
SB1109 Stand & Motor Parts List
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
15 PSB1109015 CAP SCREW M6-1 X 10 185 PSB1109185 SHAFT
30 PSB1109030 FENDER WASHER 12MM 186 PSB1109186 COLLAR
31 PSB1109031 HEX NUT M12-1.75 187 PSB1109187 MOTOR MOUN T CONNECTIN G ROD
46 PSB1109046 SET S CREW M8-1.25 X 12 188 PSB1109188 MAG SWITCH 5H SDE
70 PSB1109070 PHLP HD SCR M6-1 X 10 188-1 PSB1109188-1 MAG SWITCH COVER
73 PSB1109073 PHLP HD SCR M6-1 X 8 188-2 PSB1109188-2 MAG SWITCH BASE
81 PSB1109081 CAP SCREW M6-1 X 12 188-3 PSB1109188-3 CONTACTOR SDE MA-30 220V-240V
99 PSB 11090 99 TA P S CREW M3 X 8 188-4 PSB1109188-4 OL RELAY SDE RA-30 22-34A
100 PSB1109100 PHLP HD SCR M4-.7 X 10 188-5 PSB1109188-5 STRAIN RELIEF TYPE-3 M25-1.5
111 PSB1109111 FLAT WASHER 6MM 188-6 PSB1109188-6 STRAIN RELIEF TYPE-3 M25-1.5
170 PSB1109170 FENDER WASHER 8MM 188-7 PSB1109188-7 CON TROL PA N EL C ORD 18G 5W 98"
175 PSB1109175 MOTOR 5HP 220-240V 1-PH 188-8 PSB1109188-8 TRA NSF ORMER CORD 18G 2W 23"
175-1 PSB1109175-1 S CAPACITOR 600M 125V 1-3/4 X 3-5/16 188-9 PSB1109188-9 MOTOR CORD 12G 3W X 37"
175-2 PSB1109175-2 R CAPACITOR 60M 350V 1-3/4 X 4-5/1 6 190 PSB1109190 STRAIN RELIEF TYPE-1 19MM
175-3 PSB1109175-3 CAPACITOR COVER 1 91 PSB1109191 DC M OTOR 3/4H P 90VDC 8 A
175-4 PSB1109175-4 CENT S WITCH 16MM 3450 191-1 PSB1109191-1 BRUS H BRA CKET
175-5 PSB1109175-5 CON TACT PLATE 191-2 PSB1109191-2 MOTOR BRUSH 1 20 V (2PC SET)
175-6 PSB1109175-6 MOTOR FA N 191-3 PSB1109191-3 BRUSH COVER
175-7 PSB1109175-7 FAN COVER 1 92 PSB1109192 MOTOR MOUNT PLATE
175-8 PSB1109175-8 MOTOR JUNCTION B OX 1 93 PSB1109193 FLAT WASHER 8MM
175-9 PSB1109175-9 S TRAIN RELIEF SW-P4 1 94 PSB1109194 CAP SCREW M8-1.25 X 12
176 PSB1109176 CONTROL PAN EL ASSEMB LY 1 95 PSB1109195 COLLAR
176 -1 PSB1109176-1 C ONTROL P ANEL B OX 1 96 PSB1109196 PULLEY COVER
176 -2 PSB1109176-2 PHLP HD SCR M4-.7 X 6 1 97 PSB1109197 PULLEY
176 -3 PSB1109176-3 EXT TOOTH WASHER 4MM 199 PSB1109199 PHLP HD SCR M5-.8 X 10
176 -4 PSB1109176-4 SWITCH PEDESTAL 200 PSB1109200 FLAT WASHER 5MM
176 -5 PSB1109176-5 HEX BOLT M5-.8 X 10 201 PSB1109201 DC MOTOR CONTROL COVER
176 -6 PSB1109176-6 FLANGE B OLT M6-1 X 12 202 PSB1109202 PHLP HD SCR M5-.8 X 20
176 -7 PSB1109176-7 CIRCUIT BREA KER S WITCH 10A ZE-800 220 PSB1109220 PLATE
176 -8 PSB1109176-8 POTENTIOMETER 50K W/86" CORD 221 PSB1109221 SET S CREW M5-.8 X 20
176 -9 PSB1109176-9 CONTROL PANEL FACE PLATE 226 PSB1109226 SWITCH PANEL
176-10 PSB1109176-10 PHLP HD SCR M5-.8 X 8 227 PSB1109227 PHLP HD SCR 3/16-24 X 3/8
176-11 PSB1109176-11 SET SCREW M4-.7 X 6 228 PSB1109228 PHLP HD SCR M5-.8 X 10
176-12 PSB1109176-12 FEED SPEED ADJUSTMEN T KNOB 233 PSB1109233 SPACER 7 X 11.9 X 13.5
176-13 PSB1109176-13 POWER INDICATOR LIGHT 25MM 250V 1.2W 234 PSB1109234 CAP SCREW M5-.8 X 25
176-14 PSB1109176-14 E-STOP B UTTON RENY 250V, 22M M 235 PSB1109235 DRO S EN SOR COVER
176-15 PSB1109176-15 START S WITCH 250V, 22MM 236 PSB1109236 PHLP HD SCR M6-1 X 70
176-16 PSB1109176-16 DC MOTOR CON TROL CORD 1 8G 1W 8" 239 PSB1109239 CAB LE TIE 4"
176-17 PSB1109176-17 STOP BUTTON CORD 18G 1W 6 " 242 PSB1109242 DRO SEN SOR STRIP
176-18 PSB1109176-18 CIRCUIT BREAKER CORD 18G 2W 71" 245 PSB1109245 KEY 5 X 5 X 30 RE
177 PSB1109177 CAB IN ET STAN D 246 PSB1109246 MOTOR PULLEY
178 PSB1109178 FOOT M1 2-1.75 247 PSB1109247 FENDER WASHER 8MM
179 PSB1109179 SET SCREW M8-1.25 X 40 248 PSB1109248 HEX BOLT M8-1.25 X 20
180 PSB1109180 M OTOR A CCES S COVER 251 PSB1109251 POWER CORD 12G 3W 1 45" L6-30P
181 PSB1109181 FLA T HD SCR M6-1 X 20 252 PSB1109252 DC M OTOR C ON TROLLER
182 PSB1109182 MOTOR MOUN T PLATE 253 PSB1109253 TRAN SFORMER SP-CL-20660 220V
183 PSB1109183 HEX BOLT M8-1.25 X 40 254 PSB1109254 WIRE NUT P3
184 PSB1109184 H EX N UT M8-1 .25
-71-
Page 77
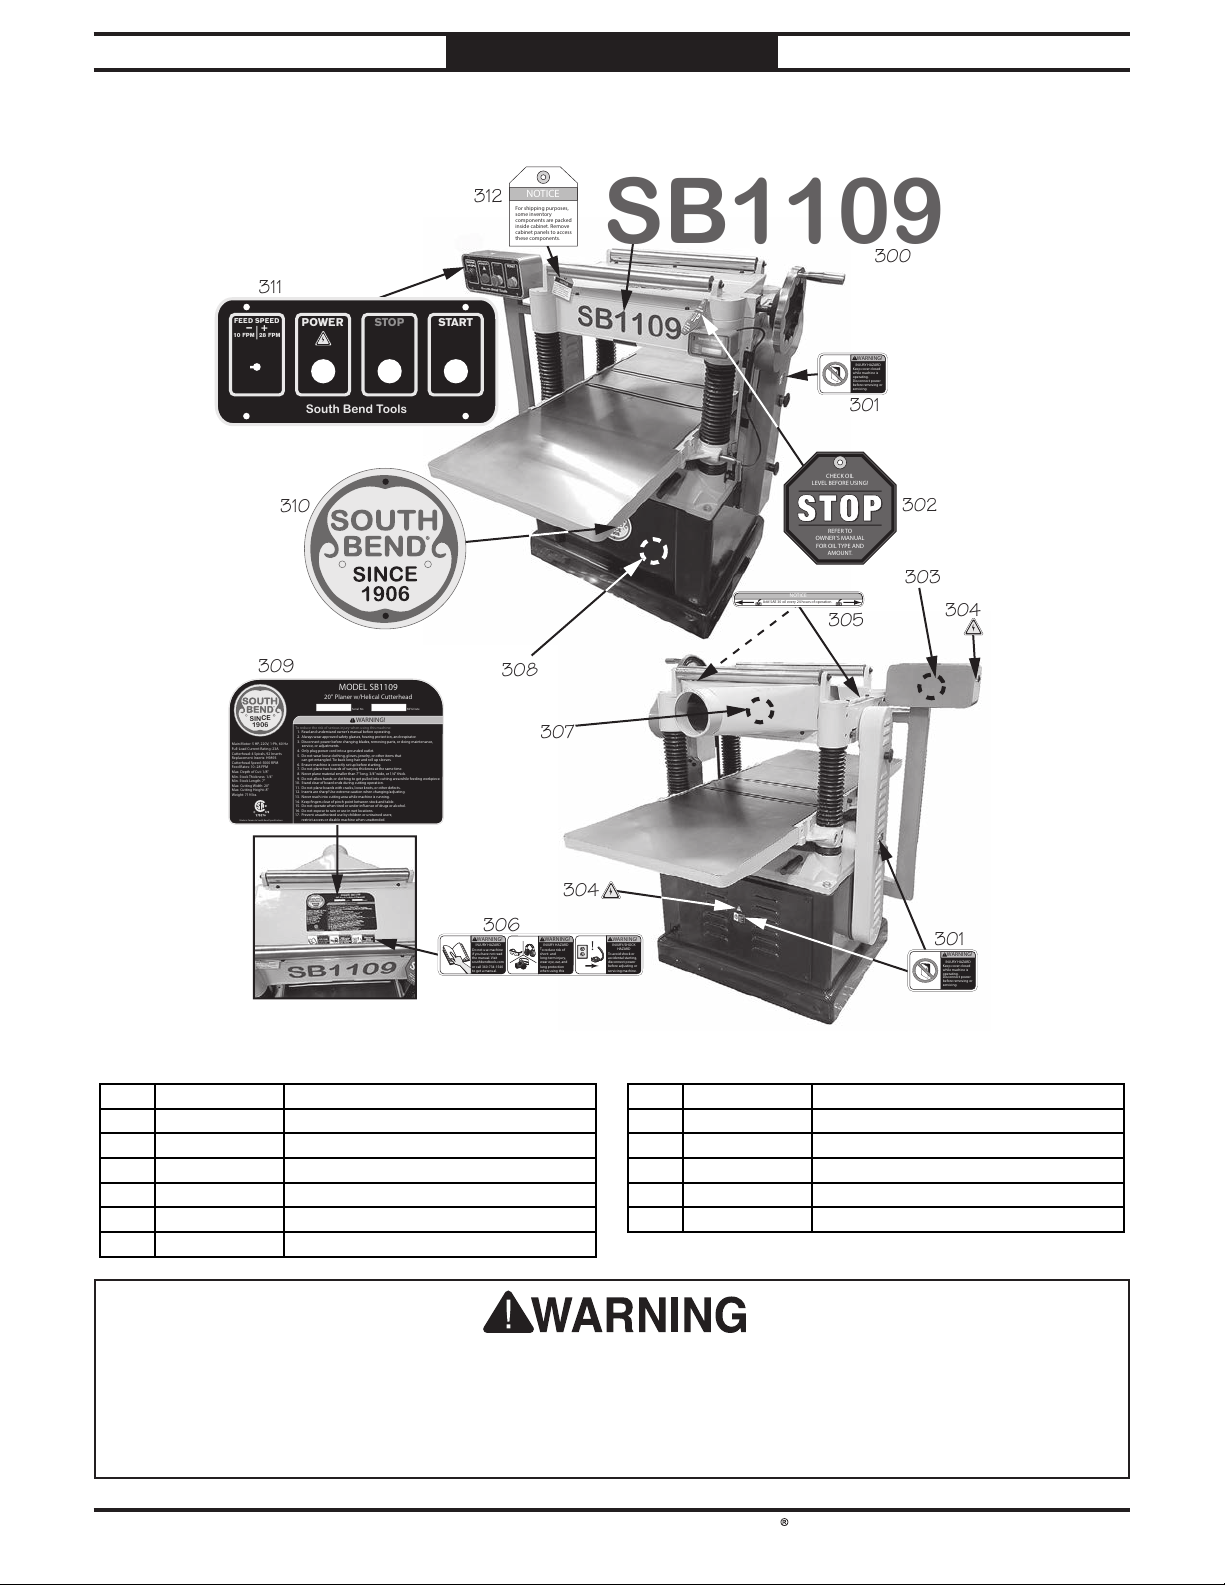
South Bend Tools
Model SB1108/ SB1109
REFER TO
OWNER’S MANUAL
FOR OIL TYPE AND
AMOUNT.
CHECK OIL
LEVEL BEFORE USING!
WARNING!
!
INJURY HAZARD
Keep cover closed
while machine is
operating.
Disconnect power
before removing or
servicing.
Add SAE 30 oil every 24 hours of operation.
NOTICE
SB1109
WARNING!
!
INJURY HAZARD
Keep cover closed
while machine is
operating.
Disconnect power
before removing or
servicing.
NOTICE
For shipping purposes,
some inventory
components are packed
inside cabinet. Remove
cabinet panels to access
these components.
South Bend Tools
POWER
STOP
START
FEED SPEED
– +
28 FPM
10 FPM
Made in Taiwan to South Bend Specications
WARNING!
!
MODEL SB1109
20" Planer w/Helical Cutterhead
MFG DateSerial No
Main Motor: 5 HP, 220V, 1-Ph, 60 Hz
Full-Load Current Rating: 23A
Cutterhead: 4 Spirals, 92 Inserts
Replacement Inserts: H9893
Cutterhead Speed: 5000 RPM
Feed Rates: 10–28 FPM
Max. Depth of Cut: 1/8"
Min. Stock Thickness: 1/4"
Min. Stock Length: 7"
Max. Cutting Width: 20"
Max. Cutting Height: 8"
Weight: 719 lbs.
To reduce the risk of serious injury when using this machine:
1. Read and understand owner’s manual before operating.
2. Always wear approved safety glasses, hearing protection, and respirator.
3. Disconnect power before changing blades, removing parts, or doing maintenance,
service, or adjustments.
4. Only plug power cord into a grounded outlet.
5. Do not wear loose clothing, gloves, jewelry, or other items that
can get entangled. Tie back long hair and roll up sleeves.
6. Ensure machine is correctly set up before starting.
7. Do not plane two boards of varying thickness at the same time.
8. Never plane material smaller than 7" long, 3/4” wide, or 1/4" thick.
9. Do not allow hands or clothing to get pulled into cutting area while feeding workpiece.
10. Stand clear of board ends during cutting operation.
11. Do not plane boards with cracks, loose knots, or other defects.
12. Inserts are sharp! Use extreme caution when changing/adjusting.
13. Never reach into cutting area while machine is running.
14. Keep ngers clear of pinch point between stock and table.
15. Do not operate when tired or under inuence of drugs or alcohol.
16. Do not expose to rain or use in wet locations.
17. Prevent unauthorized use by children or untrained users;
restrict access or disable machine when unattended.
SINCE
1906
INJURY HAZARD
Do not use machine
if you have not read
the manual. Visit
southbendtools.com
or call 360-734-1540
to get a manual.
WARNING!
!
WARNING!
!
!
INJURY/SHOCK
HAZARD
To avoid shock or
accidental starting,
disconnect power
before adjusting or
servicing machine.
WARNING!
!
INJURY HAZARD
To reduce risk of
short- and
long-term injury,
wear eye, ear, and
lung protection
when using this
301
304
302
305
301
304
306
309
311
312
300
310
308
307
303
PARTS
SB1109 Labels & Cosmetics
For Machines Mfd. Since 12/20
REF PAR T # DE SCR IPTION REF PAR T # DE SCR IPTION
300 PSB1109300 MODEL NUMBER LAB EL 30 7 PSB1109307 TOUCH -UP PAINT, SB GRAY
301 PSB1109301 DOOR CLOSED LA B EL 2 .5 X 1 .5 30 8 PSB1109308 TOUCH-UP PAINT, SB LIGHT B LUE
302 PSB1109302 STOP OIL FILL TAG 309 PSB1109309 MACHINE ID LABEL
303 PSB1109303 TOUCH-UP PA IN T, S B DARK B LUE 310 PSB1109310 SOUTH BEN D NAMEPLATE 6"
304 PSB1109304 ELECTRICITY LABEL 0.7 311 PSB1109311 CONTROL PANEL LA BEL
305 PSB1109305 ADD OIL N OTI CE 312 PSB1109312 INVENTORY SHIPPING NOTICE
306 PSB1109306 COMBO WARNIN G LA B EL
The safety labels provided with your machine are used to make the operator aware of the
machine hazards and ways to prevent injury. The owner of this machine MUST maintain the
original location and readability of these safety labels. If any label is removed or becomes
unreadable, REPLACE that label before using the machine again. Contact South Bend Tools at
(360) 734-1540 or www.southbendtools.com to order new labels.
-72-
Page 78
WARRANTY
This quality product is warranted by South Bend Tools to the original buyer for 2 years from the
date of purchase. This warranty does not apply to consumable parts, or defects due to any kind of
misuse, abuse, negligence, accidents, repairs, alterations or lack of maintenance. We do not reimburse
for third party repairs. In no event shall we be liable for death, injuries to persons or property, or for
incidental, contingent, special or consequential damages arising from the use of our products.
We do not warrant or represent that this machine complies with the provisions of any law, act,
code, regulation, or standard of any domestic or foreign government, industry, or authority. In no
event shall South Bend’s liability under this warranty exceed the original purchase price paid for
this machine. Any legal actions brought against South Bend Tools shall be tried in the State of
Washington, County of Whatcom.
This is the sole written warranty for this machine. Any and all warranties that may be implied by
law, including any merchantability or fitness, for any purpose, are hereby limited to the duration of
this warranty.
Thank you for your business and continued support.
To take advantage of this warranty, register at
can scan the QR code below to be automatically directed to our warranty registration page. Enter all
applicable information for the product.
Warranty
https://www.grizzly.com/forms/warranty, or you
WARRANT Y
southbendtools.com
Page 79
southbendtools.com
Printed In Taiwan #JPCS21259
 Loading...