

Page 1
1 (17)
www.murata.com
Rev. 2
ASSEMBLY INSTRUCTIONS FOR SCC20 0 0 S E RIES
Technical Note
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 2
2 (17)
www.murata.com
Rev. 2
Table of Contents
1 Objective ..................................................................................................................................... 3
2 Murata's 24-lead Dual In-line Package (DIL-24) ........................................................................ 3
3 DIL-24 Package Outline and Dimensions .................................................................................. 4
4 Tape and reel specifications ...................................................................................................... 5
5 Printed Circuit Board (PCB) Level Guidelines .......................................................................... 7
5.1 PCB design recommendations ............................................................................................... 7
5.2 Solder paste .......................................................................................................................... 7
5.3 Stencil .................................................................................................................................... 8
5.4 Paste printing ......................................................................................................................... 8
5.5 Component picking and placement ........................................................................................ 8
5.6 Reflow soldering .................................................................................................................... 9
5.7 Moisture sensitivity level (MSL) classification ....................................................................... 10
5.8 Inspection ............................................................................................................................ 11
5.9 Precautions .......................................................................................................................... 12
5.9.1 Mechanical shocks ....................................................................................................... 12
5.9.2 Vibration ....................................................................................................................... 12
5.9.3 Chemicals ..................................................................................................................... 13
5.9.4 Coatings ....................................................................................................................... 13
5.9.5 Vacuum level ................................................................................................................ 13
5.9.6 Air blowing .................................................................................................................... 13
5.9.7 ESD .............................................................................................................................. 14
5.9.8 Moisture ........................................................................................................................ 14
5.9.9 Mechanical stress ......................................................................................................... 14
5.10 Cleaning .............................................................................................................................. 14
6 Rework Guidelines .................................................................................................................... 14
6.1 Instructions for desoldering and removing of component ..................................................... 15
7 Environmental Aspects ............................................................................................................ 17
8 References ................................................................................................................................ 17
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 3
3 (17)
www.murata.com
Rev. 2
1 Objective
This document provides general guidelines for Printed Circuit Board (PCB) design and
assembly of Murata's SCC2000 series components. It should be emphasized that this
document serves only as a design guideline to help develop the optimal assembly
conditions. It is essential that users also use their own manufacturing practices and
experience to be able to fulfill the needs of varying end-use applications.
2 Murata's 24-lead Dual In-line Package (DIL-24)
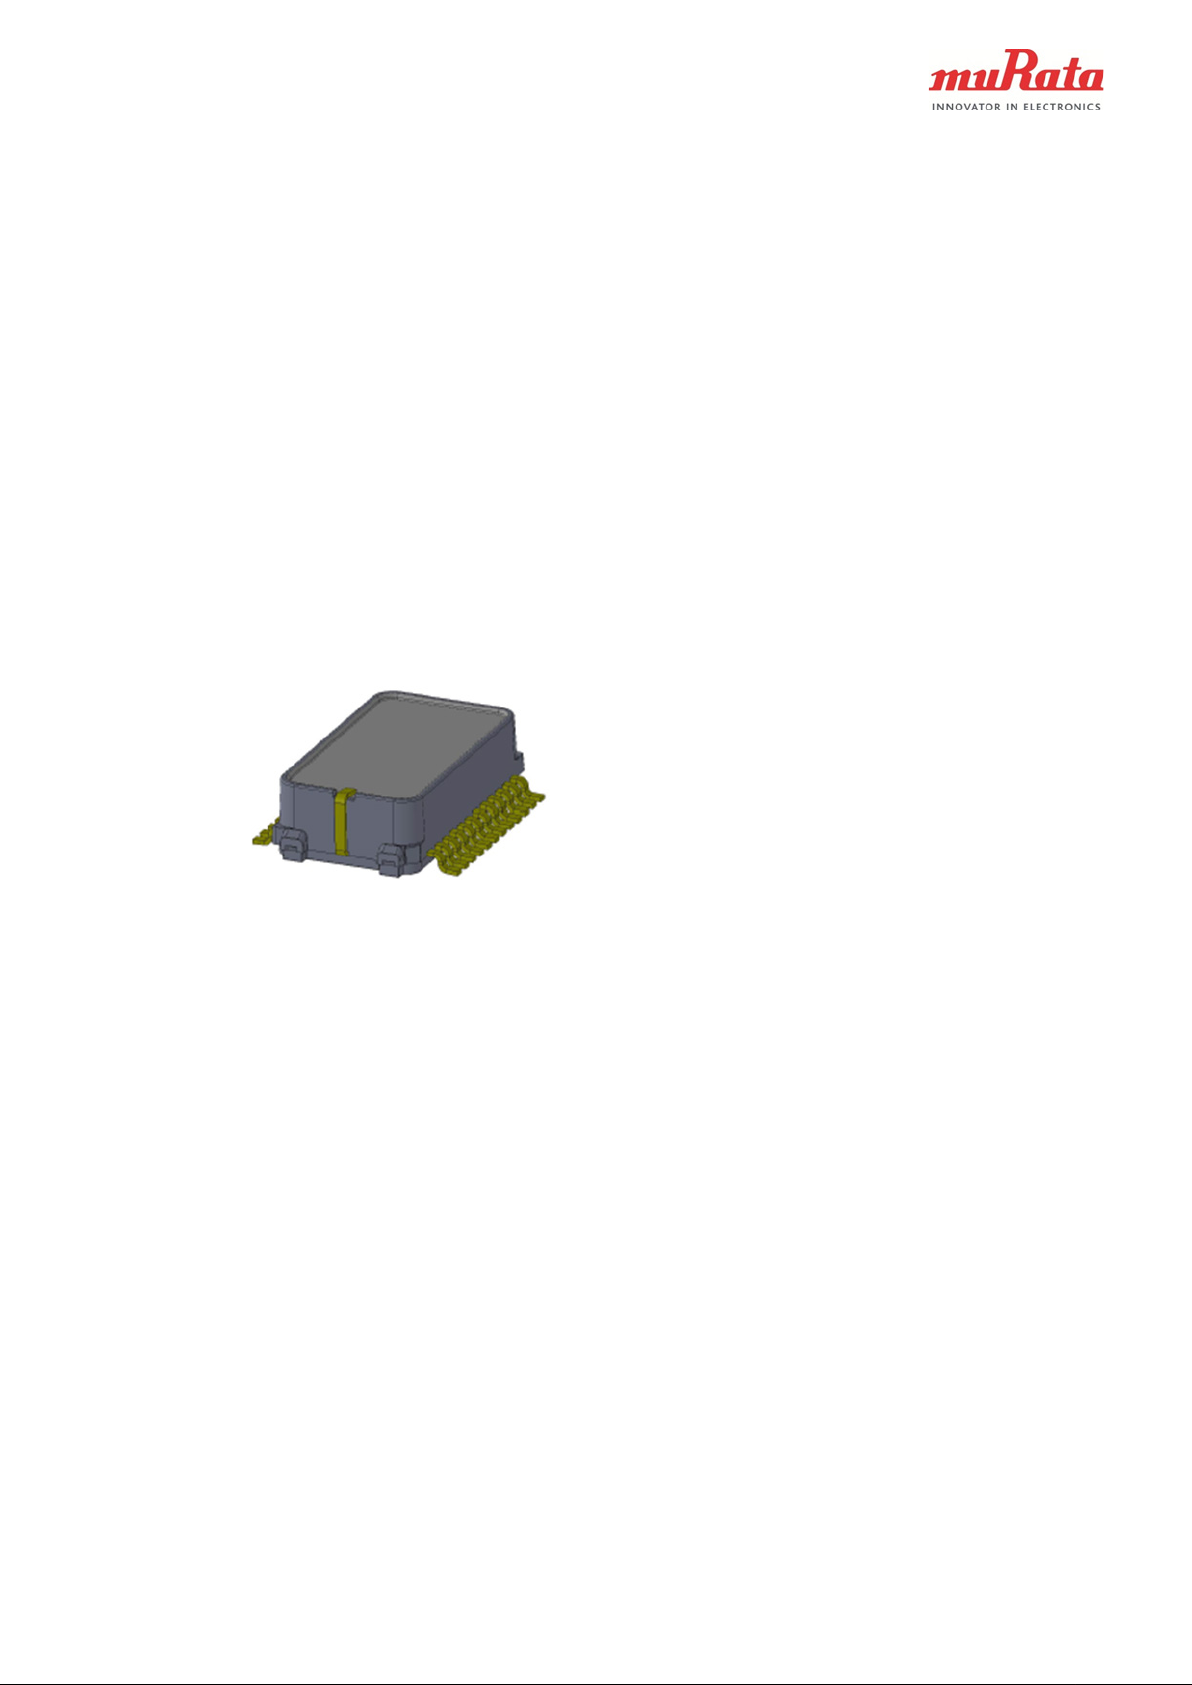
The SCC2000 series products are SMD DIL-24 components, pick-and-place mountable,
and reflow solderable. These components are completely lead-free and designed to
meet the demanding lead free soldering processes. The package consists of a premolded plastic housing, with a copper based lead frame having gull-wing type of lead
pins on the side of the package to provide electrical contact to the PCB. A metal lid is
attached to the top of the package. Package is not hermetically sealed. The DIL-24
package is presented in Figure 1.
Figure 1. Three dimensional view of the DIL-24 package.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 4
4 (17)
www.murata.com
Rev. 2
3 DIL-24 Package Outline and Dimensions
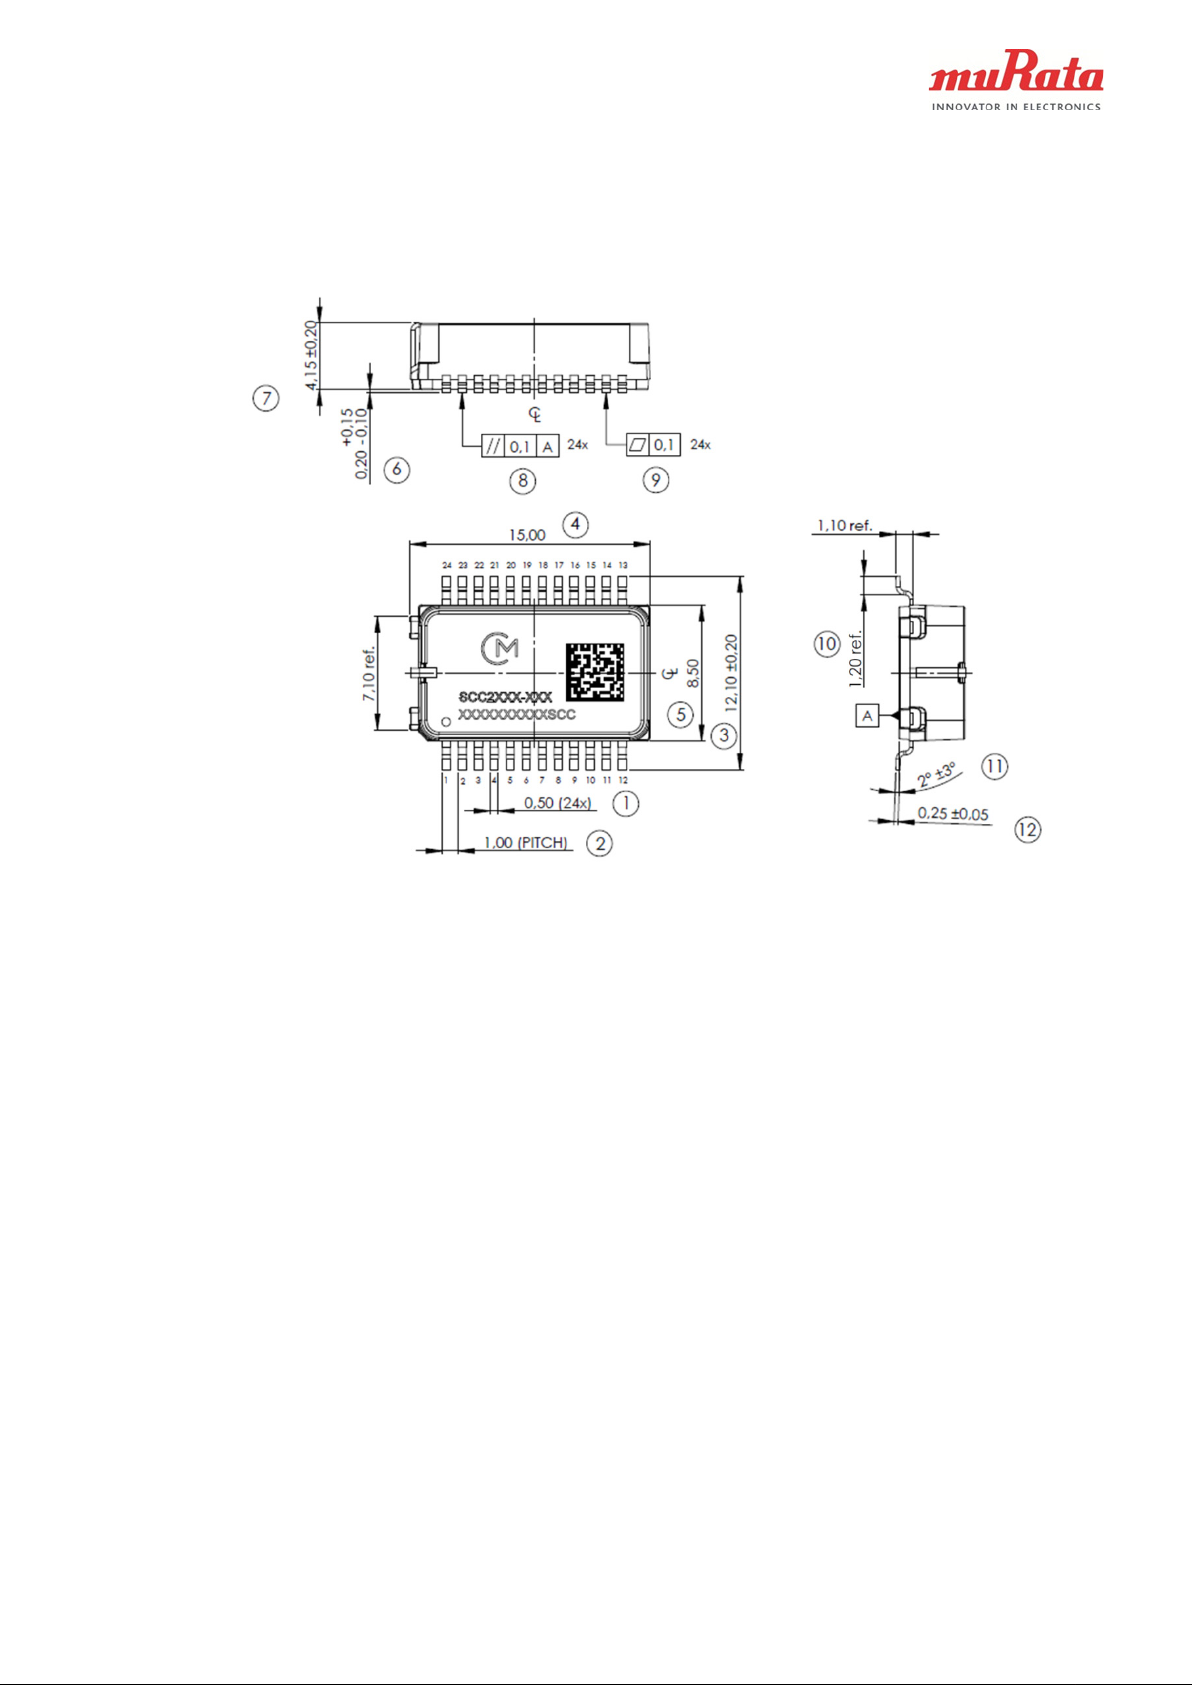
The outline and dimensions for the DIL-24 package are presented in Figure 2.
Figure 2. Outline and dimensions for DIL-24 package. Dimensions are in millimeters [mm]. All
tolerances are according to ISO 2768-f unless otherwise specified.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 5
5 (17)
www.murata.com
Rev. 2
4 Tape and reel specifications
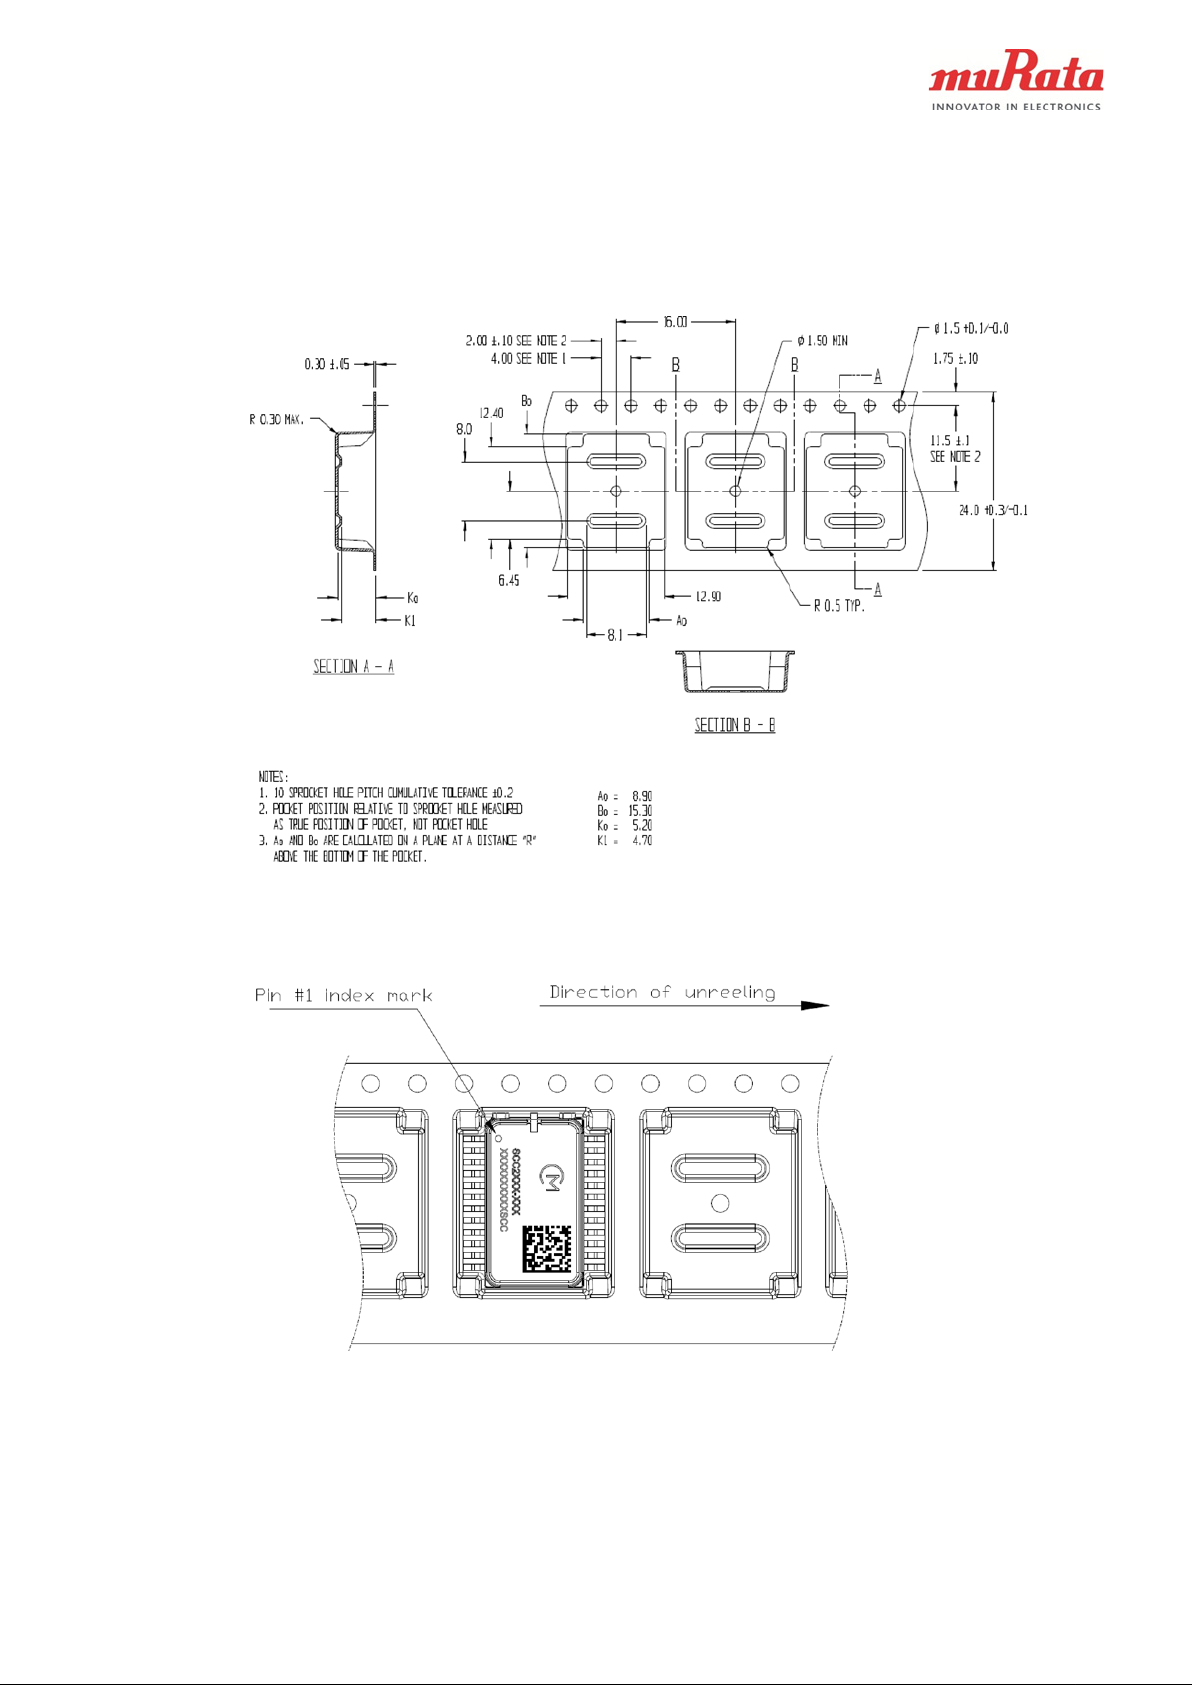
Packing tape dimensions are presented in figure 3. The unreeling direction and
component polarity on tape are presented in figure 4.
Figure 3. Packing tape dimensions for the DIL-24 Package. Dimensions are in millimeters [mm].
Murata Electronics Oy
Figure 4. Package orientation on the tape and unreeling direction on tape.
SCC2000 series Doc. No. 2845
Page 6
6 (17)
www.murata.com
Rev. 2
A N W1
W
2max
M
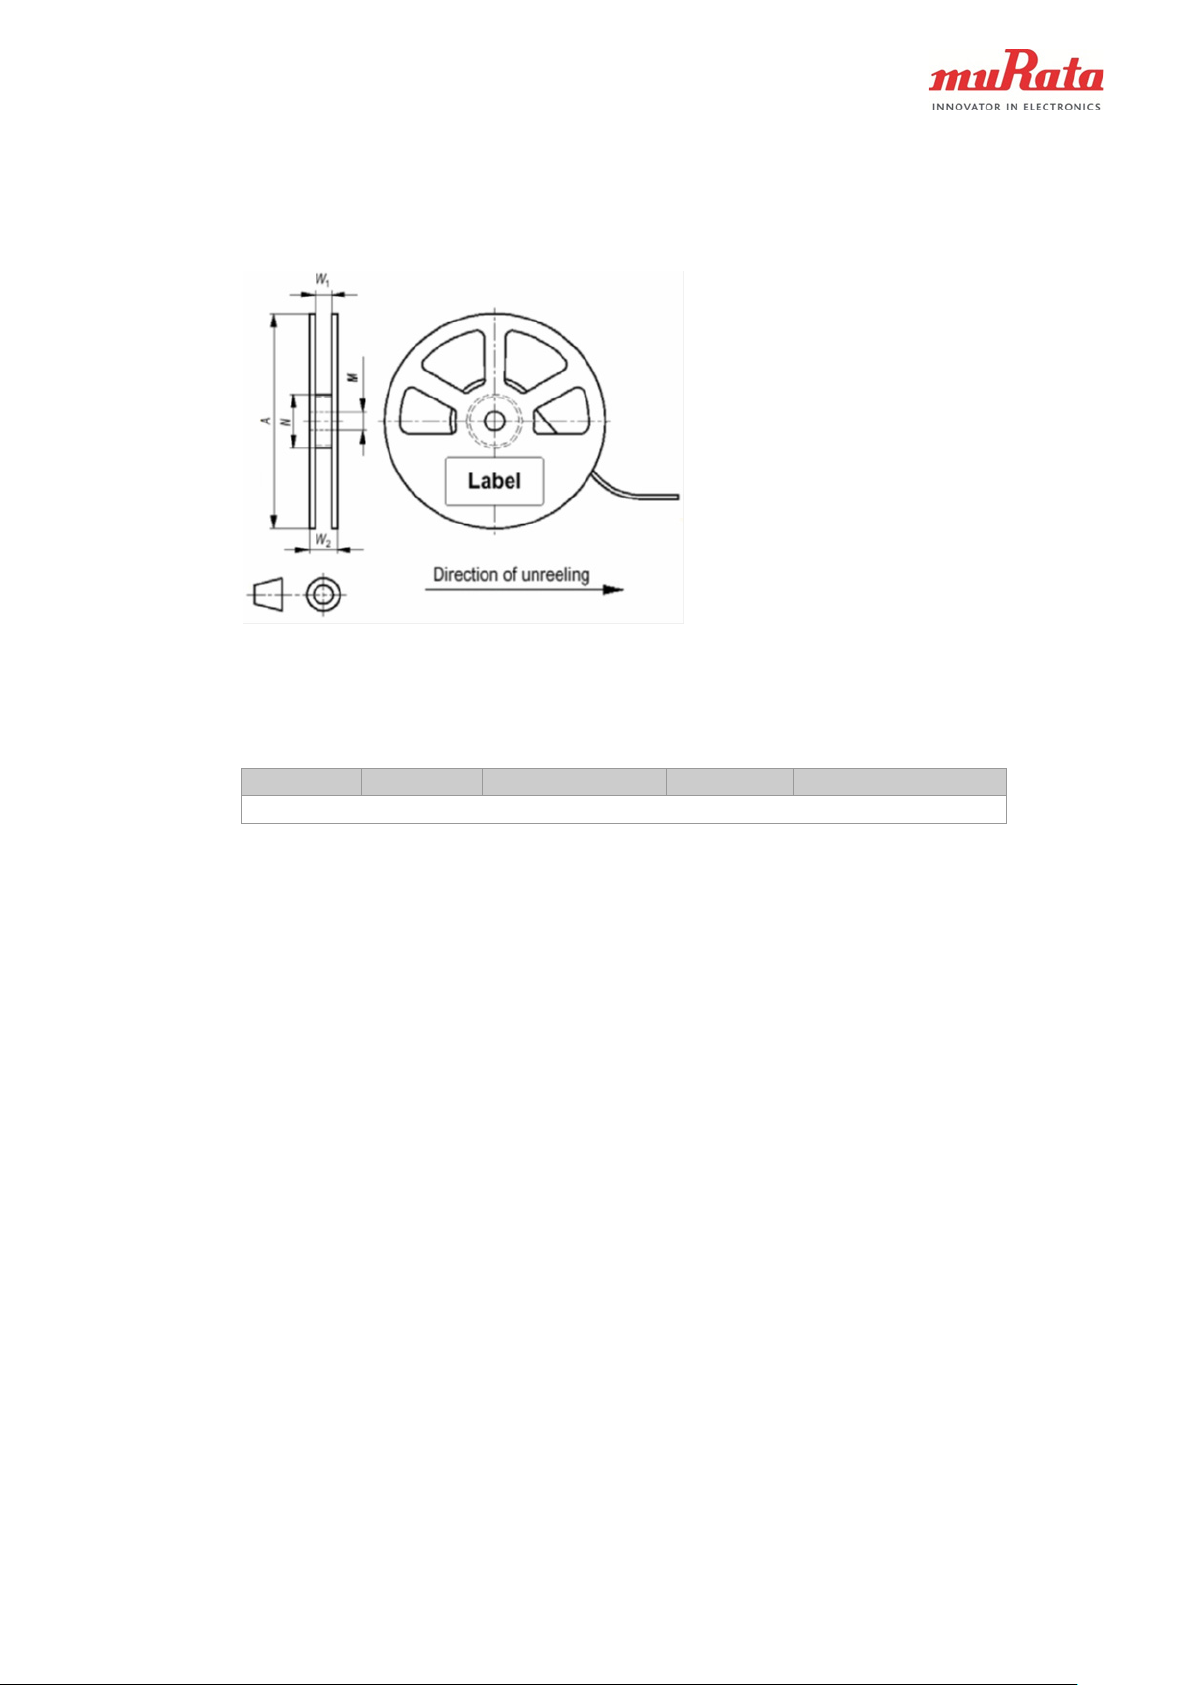
The reel dimensions are presented in figure 5 and table 1 below. Dimensions are in
millimeters [mm].
Figure 5. Reel dimensions. All dimensions are in millimeters [mm].
Table 1. Packing reel dimensions [mm].
330
100±1
32.4 (-0/+2.0) 38.4
∅ 13 (-0.2/+0.5)
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 7
7 (17)
www.murata.com
Rev. 2
5 Printed Circuit Board (PCB) Level Guidelines
5.1 PCB design recommendations
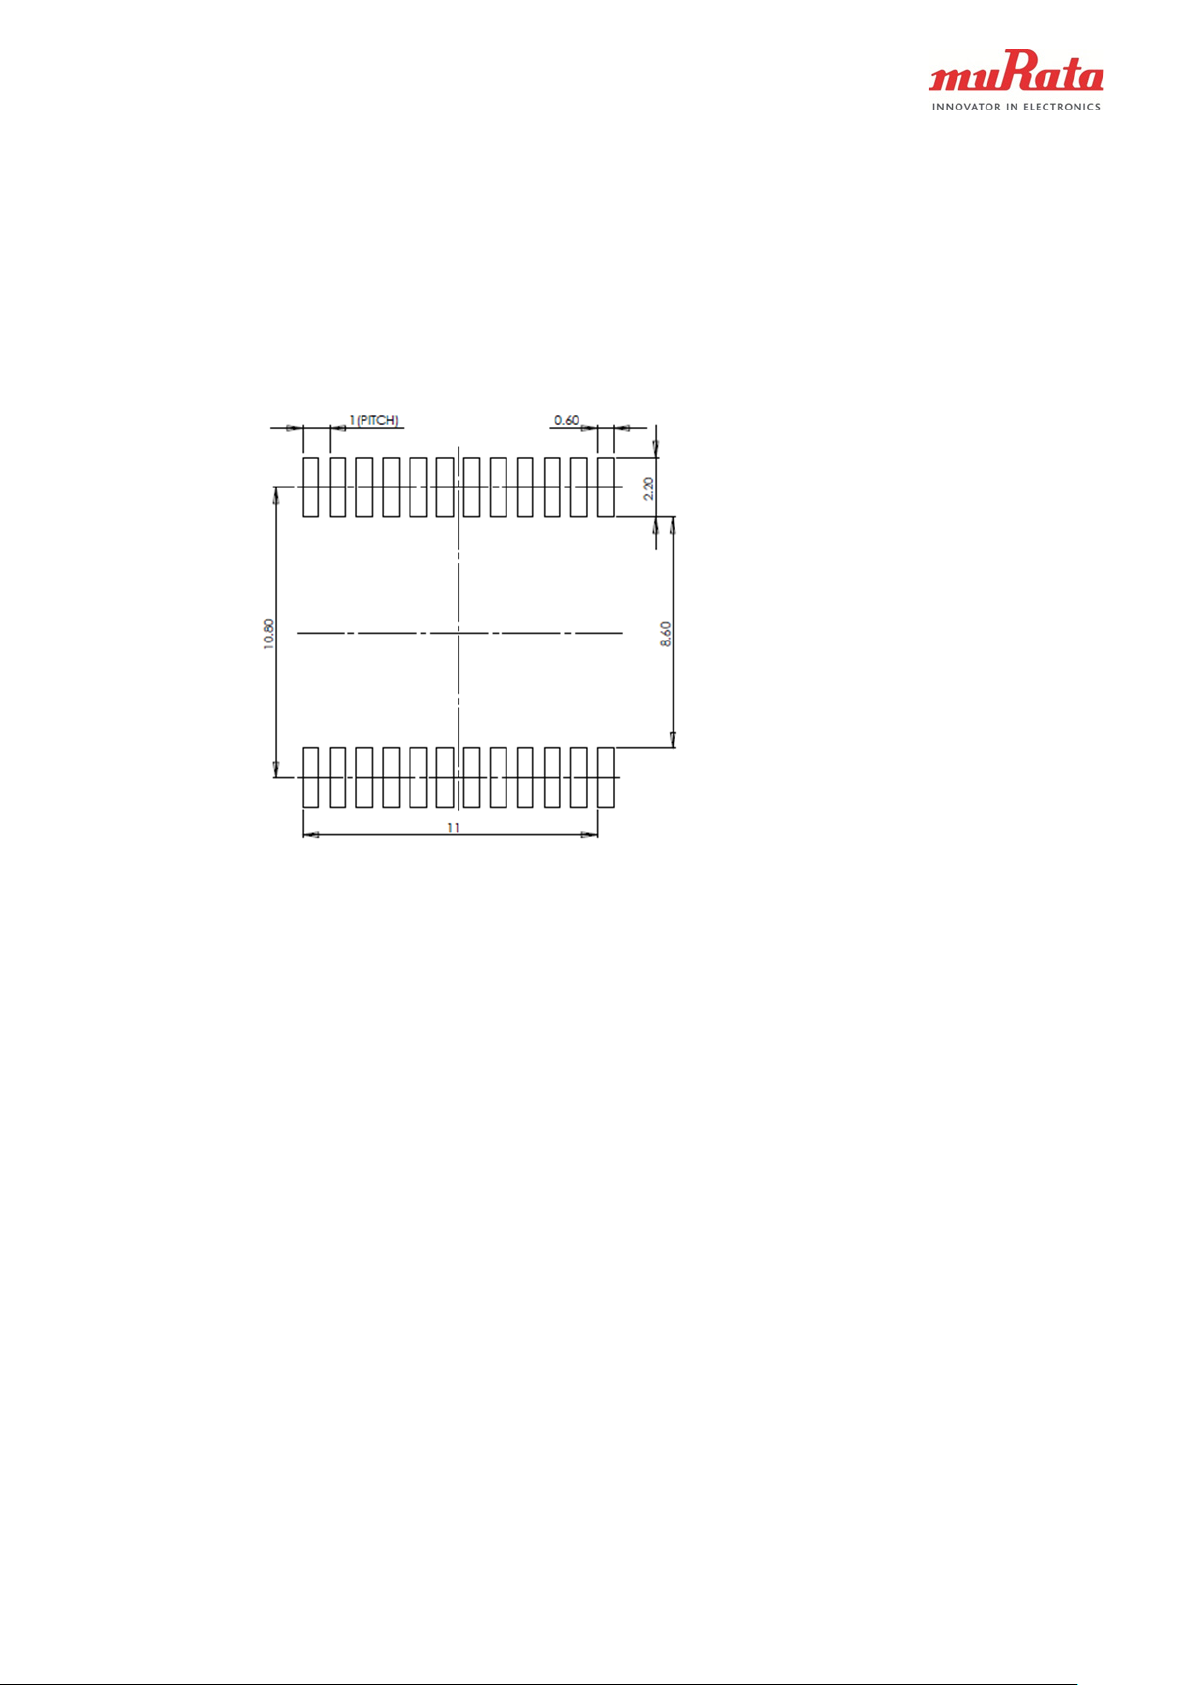
For optimal soldering and solder joint reliability results of Murata's DIL component, the
PCB terminal pads should be designed larger than the package leads. Reference
dimensions for the land pad design are presented in Figure 6. Note that this is only an
example and e.g. much narrower pads can be used and also the length can be different.
Figure 6. PCB pad lay-out for the DIL-24.
Murata's DIL packages can be soldered on commonly used substrates, e.g. FR-4,
ceramic etc. The pad metallization should be solder wettable in order to assure good
quality solder joints. For fine pitch assembly, the quality of plating is important. Generally
used circuit board finishes for fine pitch SMD soldering are NiAu, OSP, Electroless-Ag
and Electroless-Sn.
For the vibration sensitivity, it is recommended that PCB or Unit resonance modes are
analyzed to verify that there are no critical modes close to sensor oper ating frequencies
or excessive amplifications of hundreds of Gs.
5.2 Solder paste
Murata Electronics Oy
The DIL package can be soldered with lead-free SAC (tin-silver-copper) solder. The
SAC solder paste composition should be near eutectic. The melting point of lead-free
SAC solder can vary between 217–221ºC, depending on the composition of solder alloy.
In order to guarantee full RoHS compatibility lead-free solder should be used for the
soldering of Murata's DIL component. Also traditional eutectic SnPb solder can be used
for soldering the DIL packages if a lead-free process is not required. With the eutectic
SnPb solder, the melting point is 183°C.
A no-clean solder paste should be used, since the cleaning process is not
recommended. The metal lid on the pre-molded package is not fully sealed and there is
a risk that cleaning fluids might penetrate inside the package. If cleaning is used, user
SCC2000 series Doc. No. 2845
Page 8
8 (17)
www.murata.com
Rev. 2
must validate that the process does not decrease the performance or reliability of the
component. Ultrasonic agitation is strictly prohibited for Murata's MEMS components.
Ultrasonic might destroy the MEMS structures.
The solder paste which is used must be suitable for printing it through the stencil
aperture dimensions. Type 3 paste is recommended (grain size 25-45µm).
5.3 Stencil
The solder paste is applied onto the PCB using stencil printing. The stencil thickness
and aperture determines the precise volume of solder paste deposited onto the land
pattern. Stencil alignment accuracy and consistent solder volume transferring are
important parameters for achieving uniform reflow soldering results. Too much solder
paste can cause bridging and too little solder paste can cause insufficient wetting.
Generally the stencil thickness needs to be matched to the needs of all components on
the PCB taking account the co-planarity spec of Murata's DIL components.
The co-planarity of Murata's DIL components is specified max 0.1mm (100µm). For the
DIL-24 package, the recommended stencil thickness is 0,15mm (150µm). The minimum
thickness is 0,125mm (125µm).
Stencil apertures in general can be 1:1 to PWB pad sizes, or stencil apertures can be
reduced by 5-10% from all sides in regard to the PCB land pad size. This reduction of
aperture size can reduce bridging between solder joints.
5.4 Paste printing
The paste printing speed should be adjusted according to the solder paste
specifications. It is recommended that proper care of printing speed is taken during the
paste printing in order to ensure correct paste amount, shape, position, and other
printing characteristics. Neglecting any of these can cause open solder joints, bridging,
solder balling, or other unwanted soldering results.
5.5 Component picking and placement
The DIL package can be picked from the carrier tape using either vacuum assist or
mechanical type pick heads. Typically a vacuum nozzle is used. Pick up nozzles are
available in various sizes and shapes to suit a variety of different component
geometries. Murata's DIL packages are relatively large and heavy and on the other hand
accelerometers require as accurate positioning as possible. For this reason, it is
recommended that different pick up nozzles are tested to find the best one. The polarity
of the part must be assured in taping process. The orientation of the part on tape is
presented in Figure 4.
DIL packages must be placed onto the PCB accurately according to their geometry. T he
reference planes are the bottom and the side walls of the component. Placement should
be done with modern automatic component pick & place machinery using vision
systems. Recognition of the packages automatically by a vision system enables correct
centering and orientation of packages. Pin #1 is indexed by a dot mark on the
component lid as illustrated in figure 4.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 9
9 (17)
www.murata.com
Rev. 2
In the case of double sided SMT assembly, it should be noted that Murata's components
are relatively heavy and they should be glued on the PCB if they are located on the
bottom side of the PCB during the second solder reflow process. Murata's does not
recommend any specific glue for this purpose. Some of Murata's customers have used
standard epoxy based SMD adhesives.
Cover tape of reel is pressure f or mi ng type tape with g lue. Caution has to be taken care
when rolling off the cover tape to prevent the tape sticking and machine jamming.
Extensive baking should be avoided, because it can increase the sticking of the cover
tape.
5.6 Reflow soldering
A forced convection reflow oven is recommended to be used for soldering DIL
components. IR-based reflow ovens are not generally suitable for lead-free soldering.
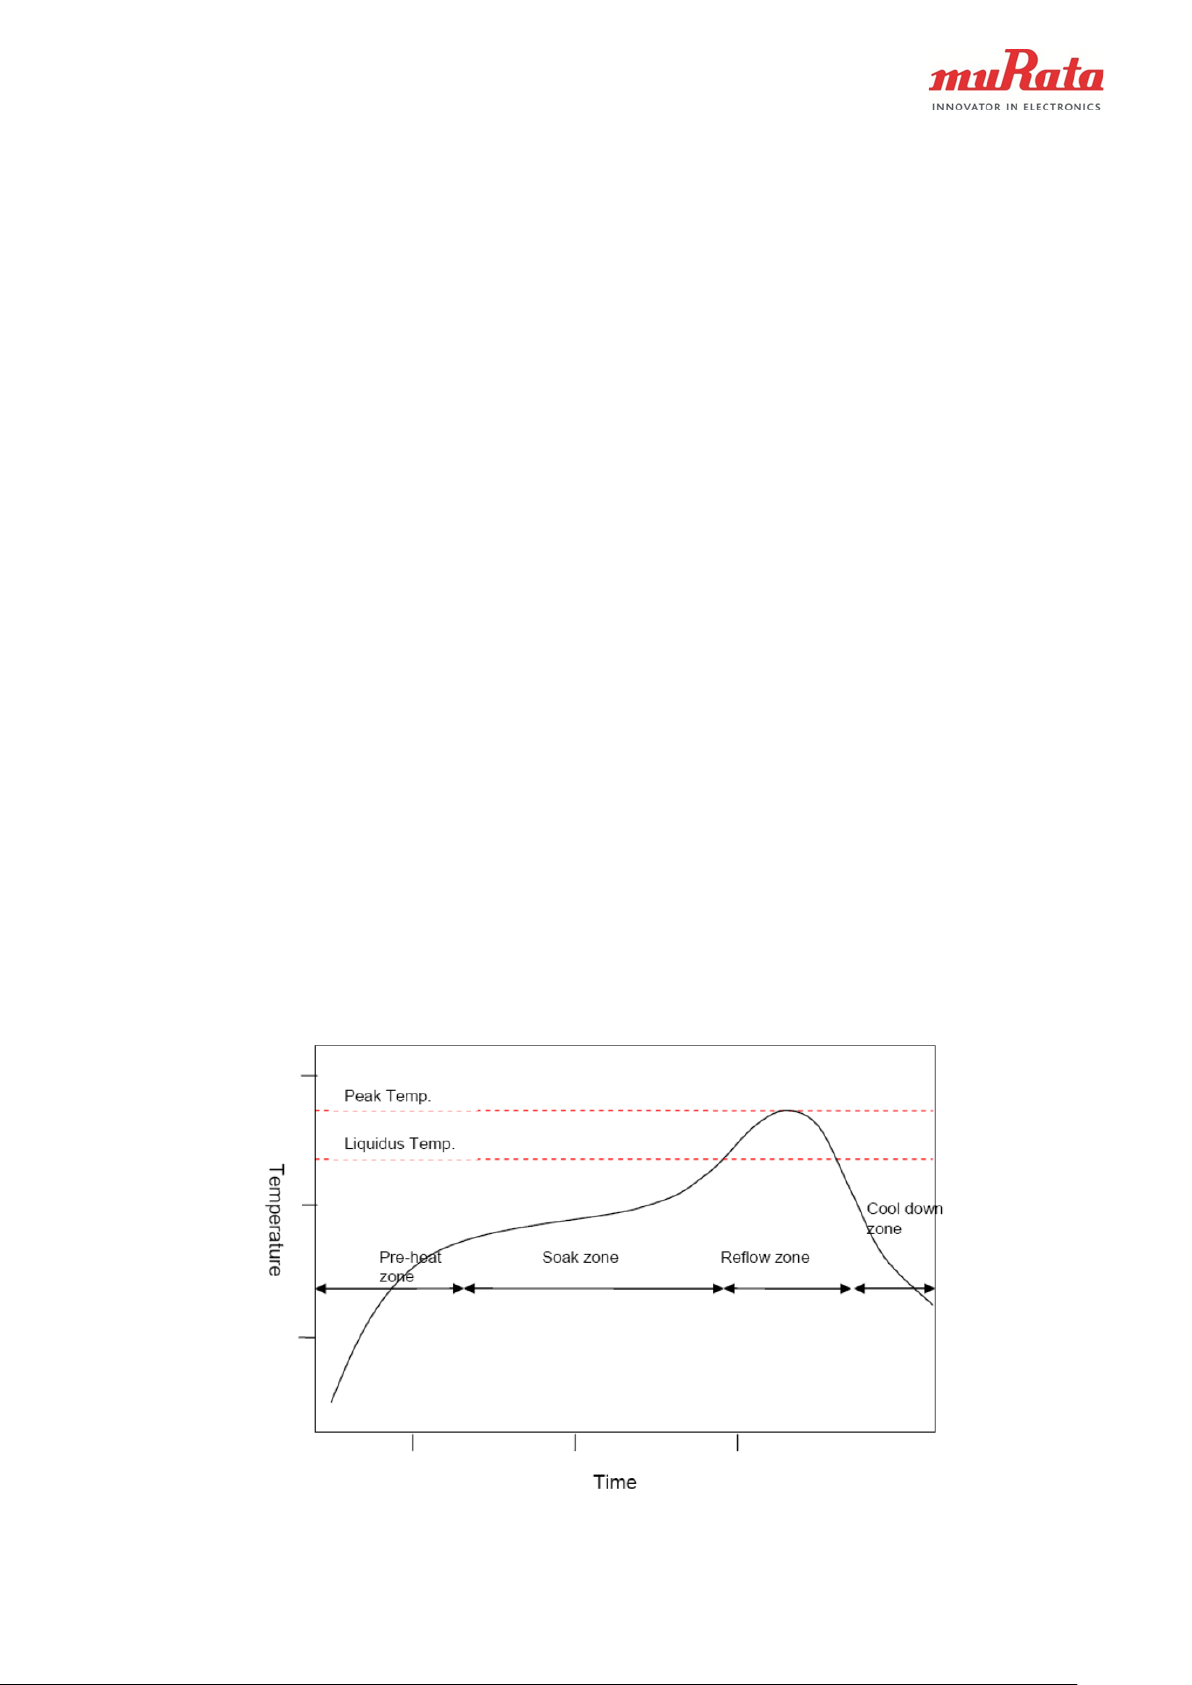
Figure 7 presents a general forced convection reflow solder profile and it also shows the
typical phases of a reflow process. The reflow profile used for soldering the DIL package
should always follow the solder paste manufacturer's specifications and recommended
profile. If washing process is done after the soldering process, it must be noted that
ultrasonic agitation wash after reflow is not allowed for Murata's DIL packaged MEMS
components. As mentioned before (section 5.2) a no-clean paste is recommended.
The typical ramp up rate is 3°C/second max. For lead-free soldering with SnAgCu solder
the pre-heat temperature zone is ~ 150°-200° and should last for ~ 60-180 seconds.
Time above the liquidus temperature (~217°C) should be ~ 60-150 seconds. The reflow
peak max. temperature should not exceed 245°. Temperature within actual peak
temperature is typically ~20-40 seconds. Ramp down rate should generally be
6°C/second max.
Maximum number of assembly reflow cycles for SCC2000 series components is three.
Reflow soldering with vacuum condition is prohibited as it may have effect for sensor
performance.
Figure 7. Typical convection reflow soldering phases and profile.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 10
10 (17)
www.murata.com
Rev. 2
The process window for lead-free soldering is narrower than for traditional eutectic SnPb
solders. Thus, caution has to be taken care when adjusting the reflow profiles. The
reflow profile should be measured using a thermo-couple measurement system. It is
recommended to use at least three thermo-couples, depending on the application. As a
general guide, one thermo-couple should be placed under a component having the
largest thermal mass, one next to the smallest component, one should be in contact with
DIL component's solder joint, and others to the appropriate spots on a circuit board, e.g.
corner, center, bottom of the board etc. The reflow profile should be adjusted according
to the measured data so that each solder joint experiences an optimal reflow profile. The
temperature gradient should be as small as possible across the circuit board. Extreme
caution has to be taken if the circuit board contains components with highly different
thermal masses.
5.7 Moisture sensitivity level (MSL) classification
The Moisture Sensitivity Level of the DIL component is Level 3 according to the
IPC/JEDEC J-STD-020D. The part is delivered in a dry pack. The manufacturing floor
time (out of bag) at the customer’s end is 168 hours. Maximum soldering peak
temperature for the DIL package is 245°C/40sec, measured from the package body.
Following instruction shall be followed:
1. Calculated shelf life in sealed bag: 12 months at < 40 °C and < 90% relative humidity
(RH).
2. Maximum soldering peak temperature for the package is 245°C/40sec, measured
from the package body.
3.
After bag is opened, devices that will be subjected to reflow solder or other high
temperature process must be
a) Stored at <10%RH
or
b) Mounted within 168 hours of factor conditions ≤30 °C/60%RH.
Note: Do not re-store devices that have exposed >10% RH conditions.
4. Devices require bake, before mounting, if:
a) Humidity Indicator Card is > 10% when read at 23 ± 5 °C
b) 3a or 3b not met.
5. If baking is required, devices may be baked for 24 hours at 85°C.
Note: Also Tape&Reel materials are applicable for baking at 85°C.
Note: Packing materials and procedures according to IPC/JEDEC J-STD-033
Note: Level and body temperature defined by IPC/JEDEC J-STD-020
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 11
11 (17)
www.murata.com
Rev. 2
5.8 Inspection
Optical and visual inspection of solder joints can be done easily, since the solder joints
are clearly seen. A visual inspection of the solder joints with conventional AOI
(automatic optical inspection) system can be used. Also X-ray inspection can be used.
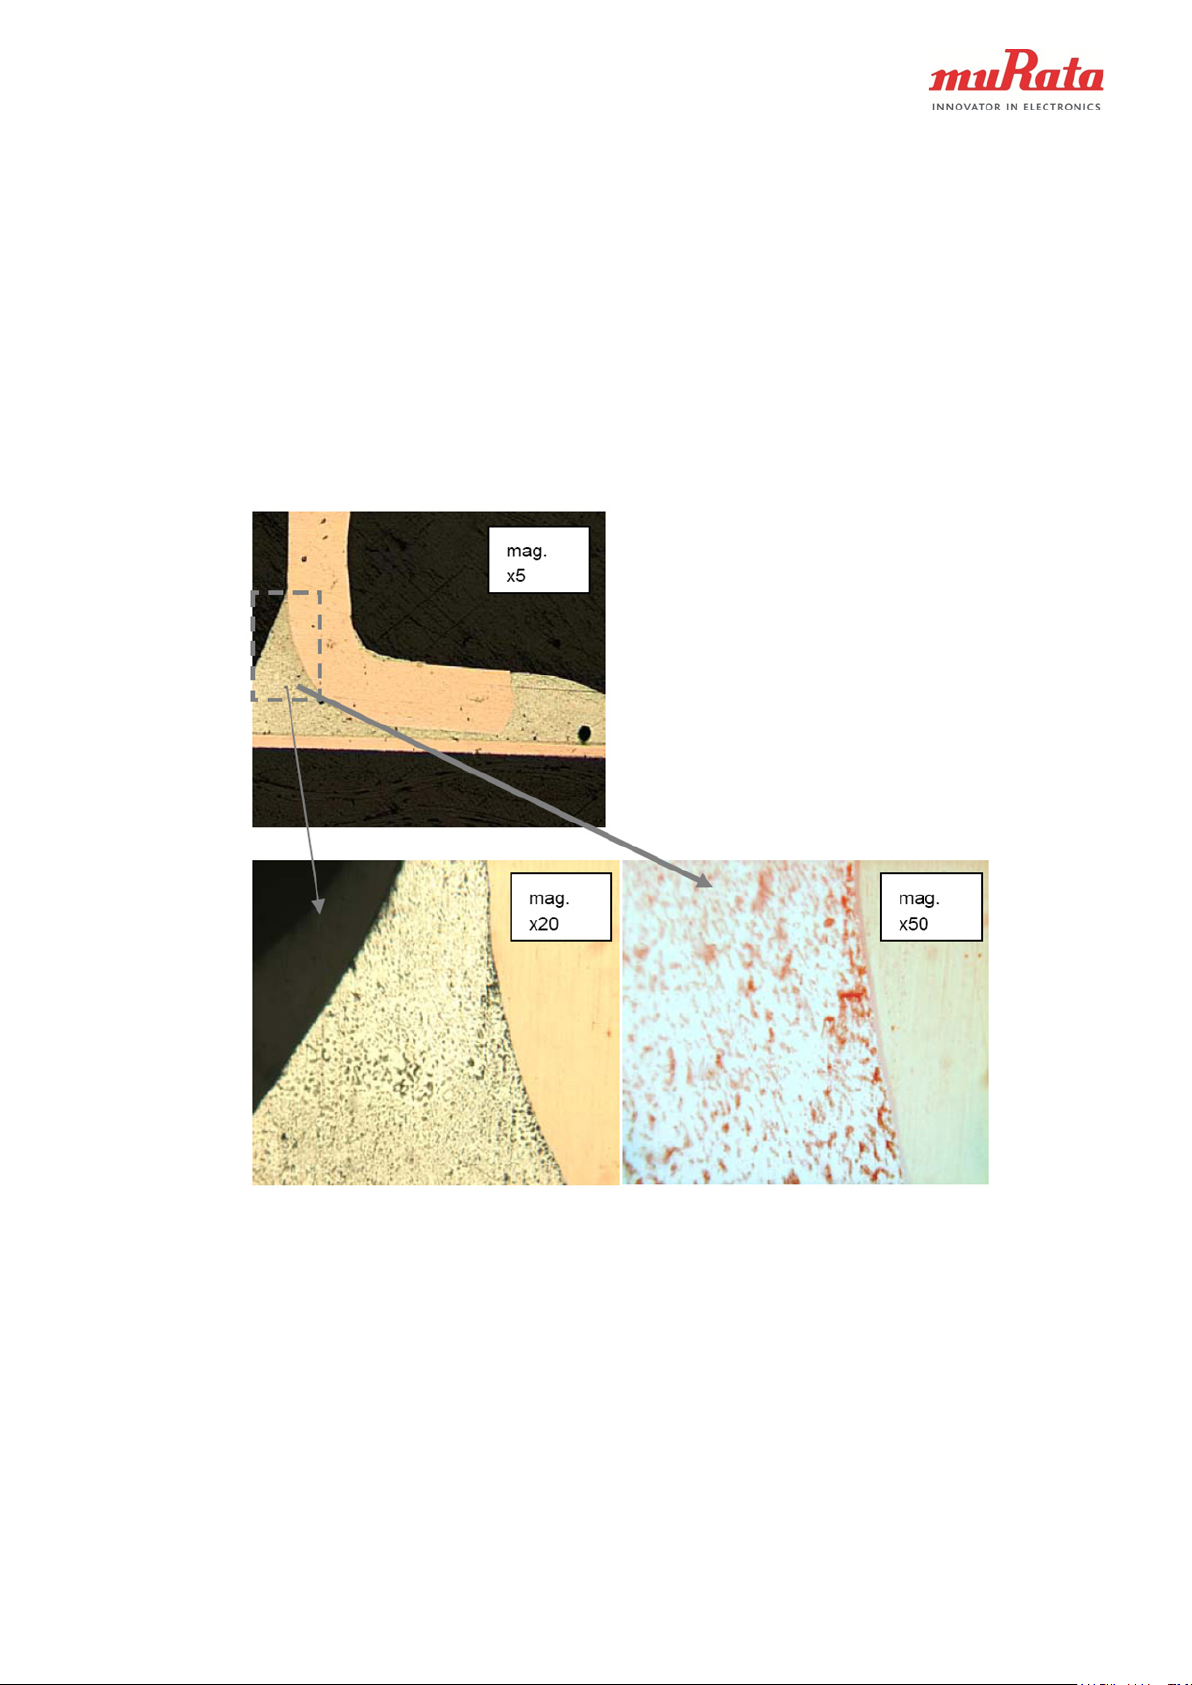
Cross-sectional analysis is also an approved method to inspect how well solder has
wetted the pads of component. Cross-sectional analysis is not used for production
inspection, but if required, it can be used to establish and optimize the component
assembly process parameters Cross-sectioning is a destructive inspection method. An
example of a DIL solder joint cross-section is presented in Figure 8.
Figure 8. Cross-section of the DIL package lead's solder joint (with eutectic SnPb solder).
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 12
12 (17)
www.murata.com
Rev. 2
5.9 Precautions
MEMS sensors are mechanically and electrically sensitive components. Following
sections describe typical processes or treatments, but are not limited to, which may be
harmful for sensor component. Exceeding these limits or neglecting these guidelines
may lead to malfunction of sensor component.
The reliability requirements for the devices are applied and validated according to AECQ100 Rev. G.
5.9.1 Mechanical shocks
Shocks may cause mechanical damage to the internal structures of MEMS sensor,
causing malfunction of sensor, therefore mechanical shocks should be avoided. The
level depends heavily on the pulse width and shape and should be evaluated case by
case. As a general guideline, the lighter assembly or part, the higher shock levels will be
generated on sensor component. Dropped components shall not be used and shall be
scrapped.
Reference tests:
1. Mechanical Shock JEDEC JESD22-B104, Y1 plane, 5 pulses, 0.5 msec duration,
1500 g peak acceleration.
2. Package Drop AEC-Q100 Rev G, device drop on each of 6 axes once from a height
of 1.2m onto a concrete surface.
5.9.2 Vibration
Sensor components are mechanical devices and especially sensitive to repetitive
vibrations and shocks, therefore vibration of the device should be avoided both prior to
or during assembly. Many assembly processes can induce vibration, typical ones being
PCB singulation, mechanical shocks, transportation, friction welding and ultra-sonic
cleaning.
Reference test:
1. (1) Variable Frequency Vibration, JEDEC JESD22-B103, 20 Hz to 2 KHz to 20 Hz
in >4 minutes, 4X in each orientation, 50 g peak acceleration.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 13
13 (17)
www.murata.com
Rev. 2
5.9.3 Chemicals
Sensor components shall not be exposed to:
• Chemicals which are known to react with silicones, such as solvents. These are for
example used in various cleaning processes
• Chemicals with high impurity levels, such as Cl-, Na+, NO3-, SO4-, NH4+
• Pressurized low molecular gas such as He or H2, used for example in leak test for
hermetical sealing
• Materials with high amount of volatile content, like solvents
Materials containing halogens (F, Br, I or Cl), halides, their compounds or phosphorus
containing materials (such as in flame retardants, thermal stabilizers in plastics, Bromine
in PCB material or halogens/halides in soldering paste) shall be avoided in close vicinity
of sensor component.
If heat stabilized polymers are used in application, user should check that iodine, or
other halogen, containing additives are not used. Iodide compounds are known to cause
issues with gold aluminum interconnects. User should also check that excessive amount
of I, Br or other halogen containing additive are not used. Quantitative value is
depending on number of factors, including the total volume of such halogen material,
stability of halogen within material, hermeticity level of application and temperature,
among others.
Life-time reliability tests should always be performed at application level to validate the
end product against life-time requirements/mission profile, as corrosion effects heavily
depend on the final construction of application, temperature, time and other application
specific factors.
5.9.4 Coatings
Coatings on sensor component are not generally recommended. Coating penetration
inside the component is high risk for performance change. If coating is required, the
effect of coating on sensor component reliability and electrical performance has to be
evaluated case by case. As a general guideline, lower the viscosity or higher the
modulus of coating, higher the probability of adverse effects on sensor component.
Sealing of the component lid is prohibited.
5.9.5 Vacuum level
Vacuum levels lower than 0.4 bar shall not be applied on sensor component. Fast
pressure changes of over 0.5 bar/min should be avoided. Example processes can be
vacuum sealing or pressure testing of the device.
5.9.6 Air blowing
Heavy compressed air blowing directly onto sensor component shall be avoided. Air
blowing could be used for example during cleaning of the PCB.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 14
14 (17)
www.murata.com
Rev. 2
5.9.7 ESD
Sensor components are electrical devices. Sensor components should be handled
under good ESD practices and ESD discharges should be avoided. The following
numbers are absolute maximum ratings:
‒ ±500 V charged device model
‒ ±2 kV human body model
5.9.8 Moisture
Sensor components are moisture sensitive devices, classified as MSL3 level. Guidelines
defined by PC/JEDEC J-STD-033 shall be followed.
5.9.9 Mechanical stress Mechanical stress due to PCB bending, molding and potting may affect the sensor
performance. Excessive stress due to PCB bending shall be avoided. If molding or
potting material is hard material, contact to sensor shall be avoided.
5.10 Cleaning Items listed in section “5.9 Precautions” are applied to cleaning also. Examples of
cleaning procedures which may have a negative effect on the sensor component
performance or functionality are:
- Wet cleaning with solvent
- Ultrasonic
- Heavy air blowing
- Plasma cleaning with vacuum
6 Rework Guidelines
If it becomes necessary to rework a SCC2000 series component, the preferred way to
remove the component is by hot air. Use of a hot air rework station with a vacuum
chuck, is the preferred method. A key issue in using hot-air is preventing thermal
damage to the component or adjacent components.
If hot air rework station is not available, rework with thermal tweezers is also an
acceptable alternative
Removing of the component with hot iron only is difficult as it is easy to get the part too
hot and destroy it. It is not recommend method if failure analysis or re-use of the
component is desired.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 15
15 (17)
www.murata.com
Rev. 2
6.1 Instructions for desoldering and removing of component
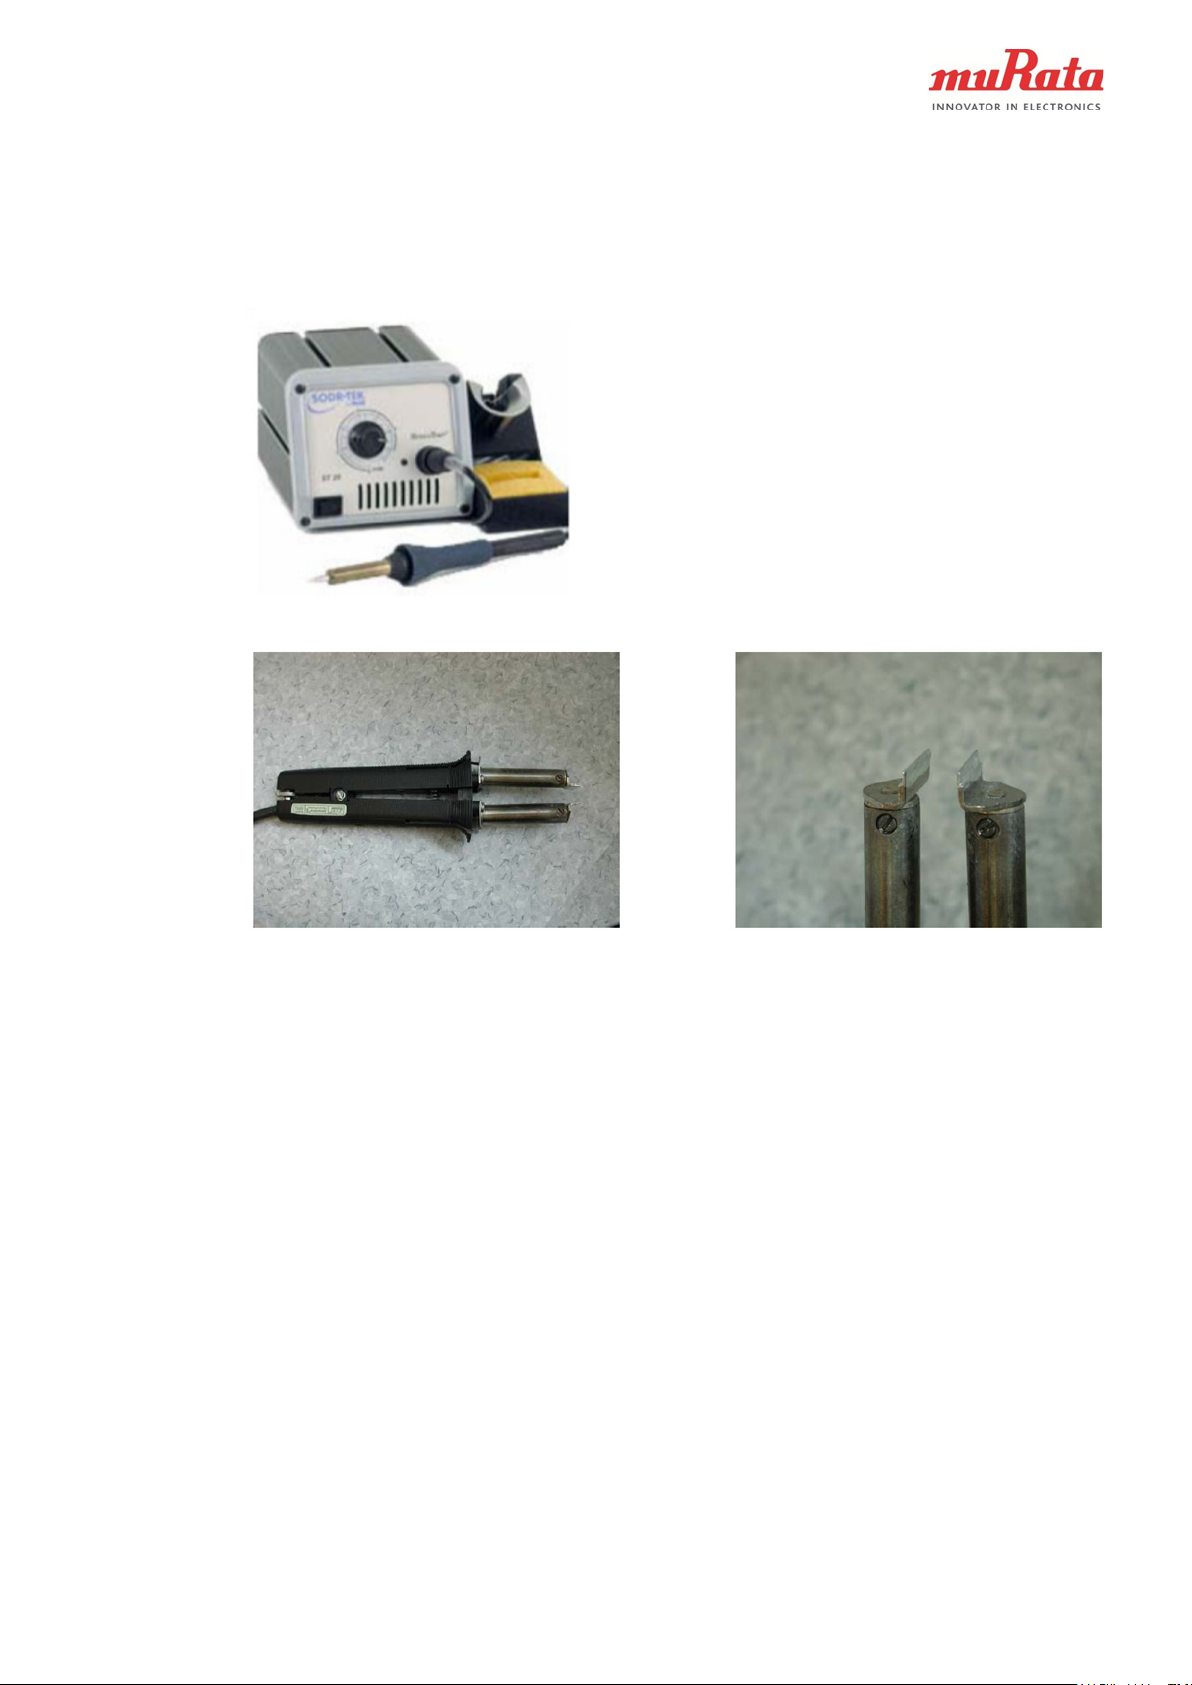
Soldering Station (Pace SensaTemp ST25E-PS90) and thermal tweezers (Pace
Thermotweez) with Pace 1121-0416-P1 tool head are used for de-soldering and
removing of the component.
Figure 9. Pace SensaTemp ST25E-PS90
Figure 10. Thermal tweezers, Pace Thermotweez. Figure 11. Tool head, Pace 1121-0416-P1.
The plastic molding compound on the component is LCP (liquid crystal polymer) which
withstands very high temperatures and is good material for Pb-free assembly. LCP's
melting point is 335ºC. However, the mechanical properties start to change already near
280ºC. If the pins are heated too long the plastic around pin will be softened and if there
at the same time is some stress on the pin there is a risk that pin might move and cause
increased reliability or wirebond break inside housing.
In order to melt all pins simultaneously, tweezers are recommended for de-soldering of
the component. Also with tweezers, special care must be taken if failure analysis or reuse of the component is desired.
In the component removal process, the temperature setting in soldering station is
normally +315ºC. The temperature on the tip of the tool is 270...275ºC. Tool is pressed
against pins only for few seconds. Same temperature is used both for Pb-free and
SnPb-solder joints, even though SnPb solders melt already below 200ºC. Some
temperature adjustment might be needed. Especially if tool head is old and 'dirty'
temperature needs to be increased.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 16
16 (17)
www.murata.com
Rev. 2
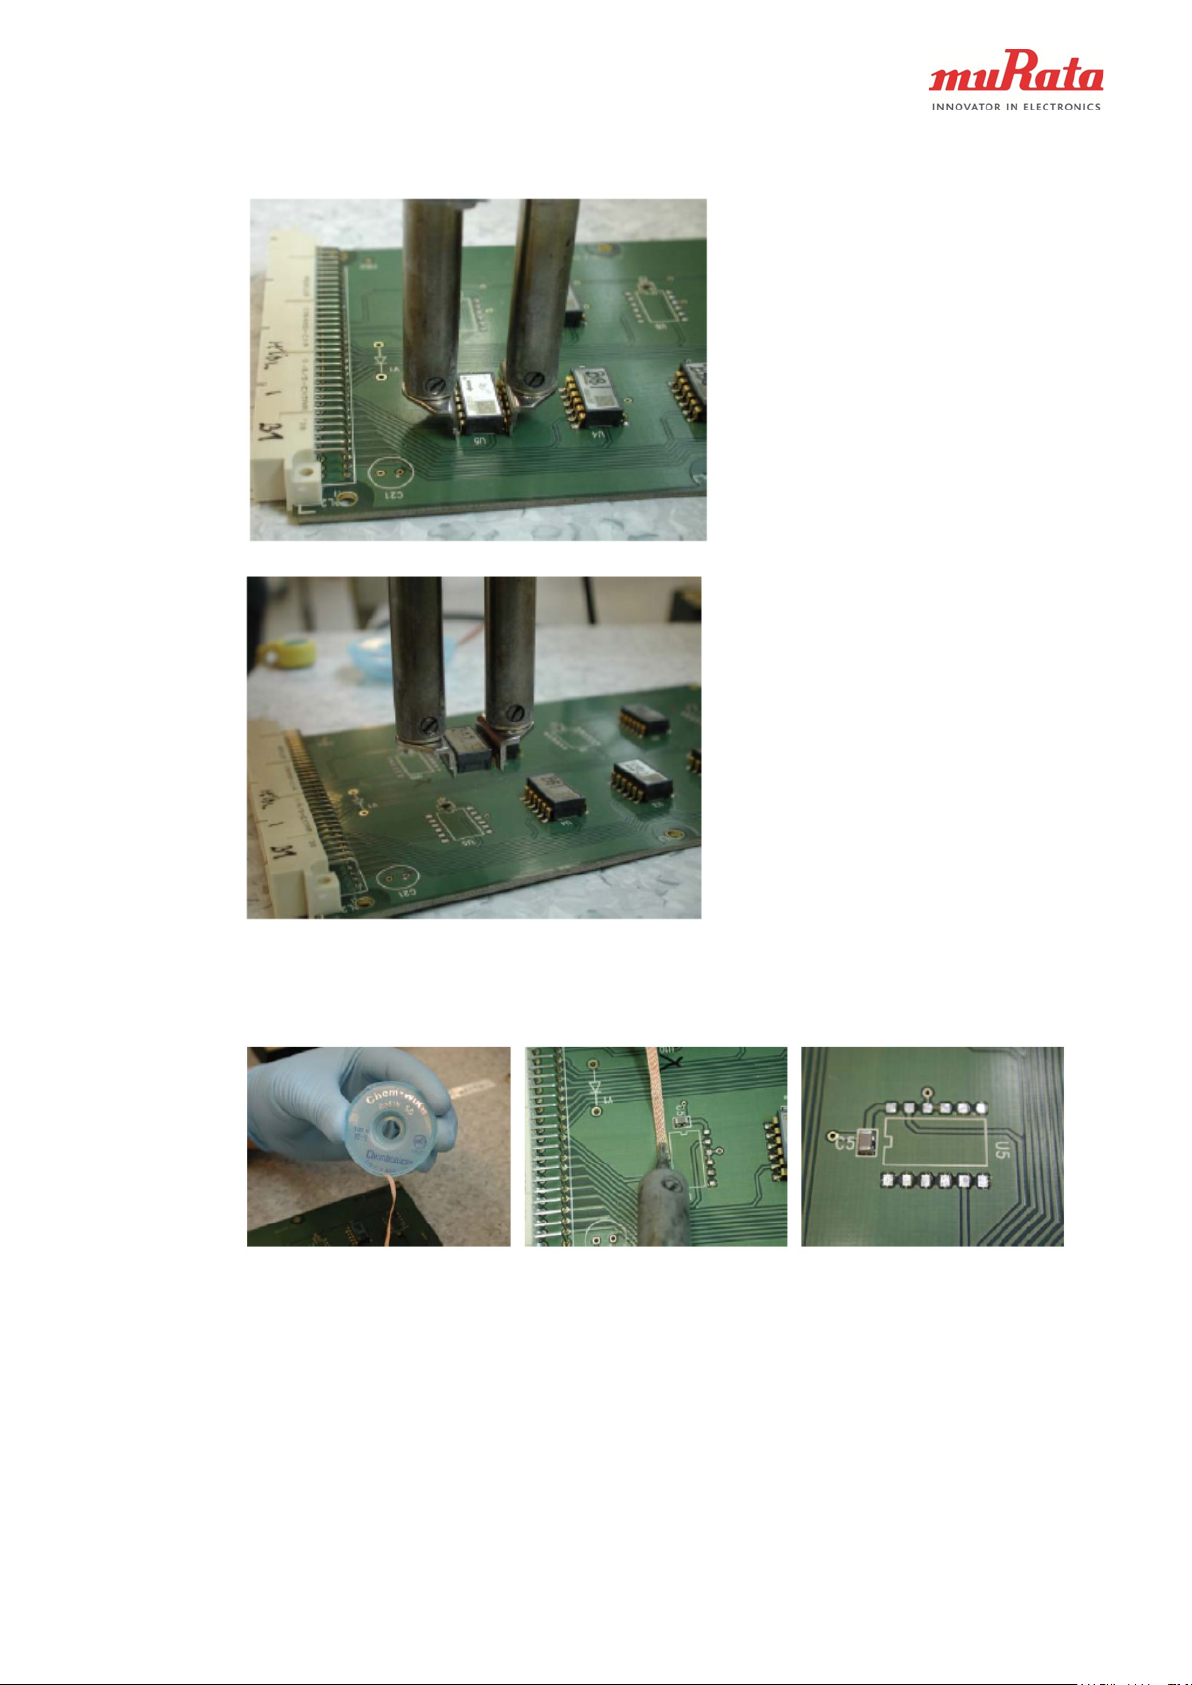
Figure 12. Tool head is carefully pressed around component and kept in this position for few
seconds.
Figure 13. Immediately after solder melting, component is lifted.
Remove the solder from the PCB using either a solder vacuum or solder braid making
sure to clean the area of solder thoroughly.
Figure 14. Soldering iron and solder braid used for solder removal.
Note that the performance and the reliability of the reworked component may
have decreased due to the rework operation! Murata does not recommend rework.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
Page 17
17 (17)
www.murata.com
Rev. 2
7 Environmental Aspects
Murata Electronics Oy respects environmental values and thus, its DIL packages are
lead-free and RoHS compatible. Murata Electronics’ sensors should be soldered with
lead-free solders in order to guarantee full RoHS compatibility.
8 References
JEDEC / Electronic Industries Alliance, Inc. Moisture/Reflow Sensitivity Classification for
Non-Hermetic Solid State Surface Mount Devices (J-STD-020D).
Handling, Packing, Shipping and Use of Moisture/Reflow Sensitive Surface Mount
Devices (IPC/JEDEC J-STD-033).
Murata Electronics Oy reserves all rights to modify this document without prior notice.
Murata Electronics Oy
SCC2000 series Doc. No. 2845
 Loading...