

Page 1
READ THIS FIRST
Model G0948
***IMPORTANT UPDATE***
For Machines Mfd. Since 08/21
and Owner's Manual Printed 09/21
For questions or help with this product contact Tech Support at (570) 546-9663 or [email protected]
The following change was recently made since the owner's manual was printed:
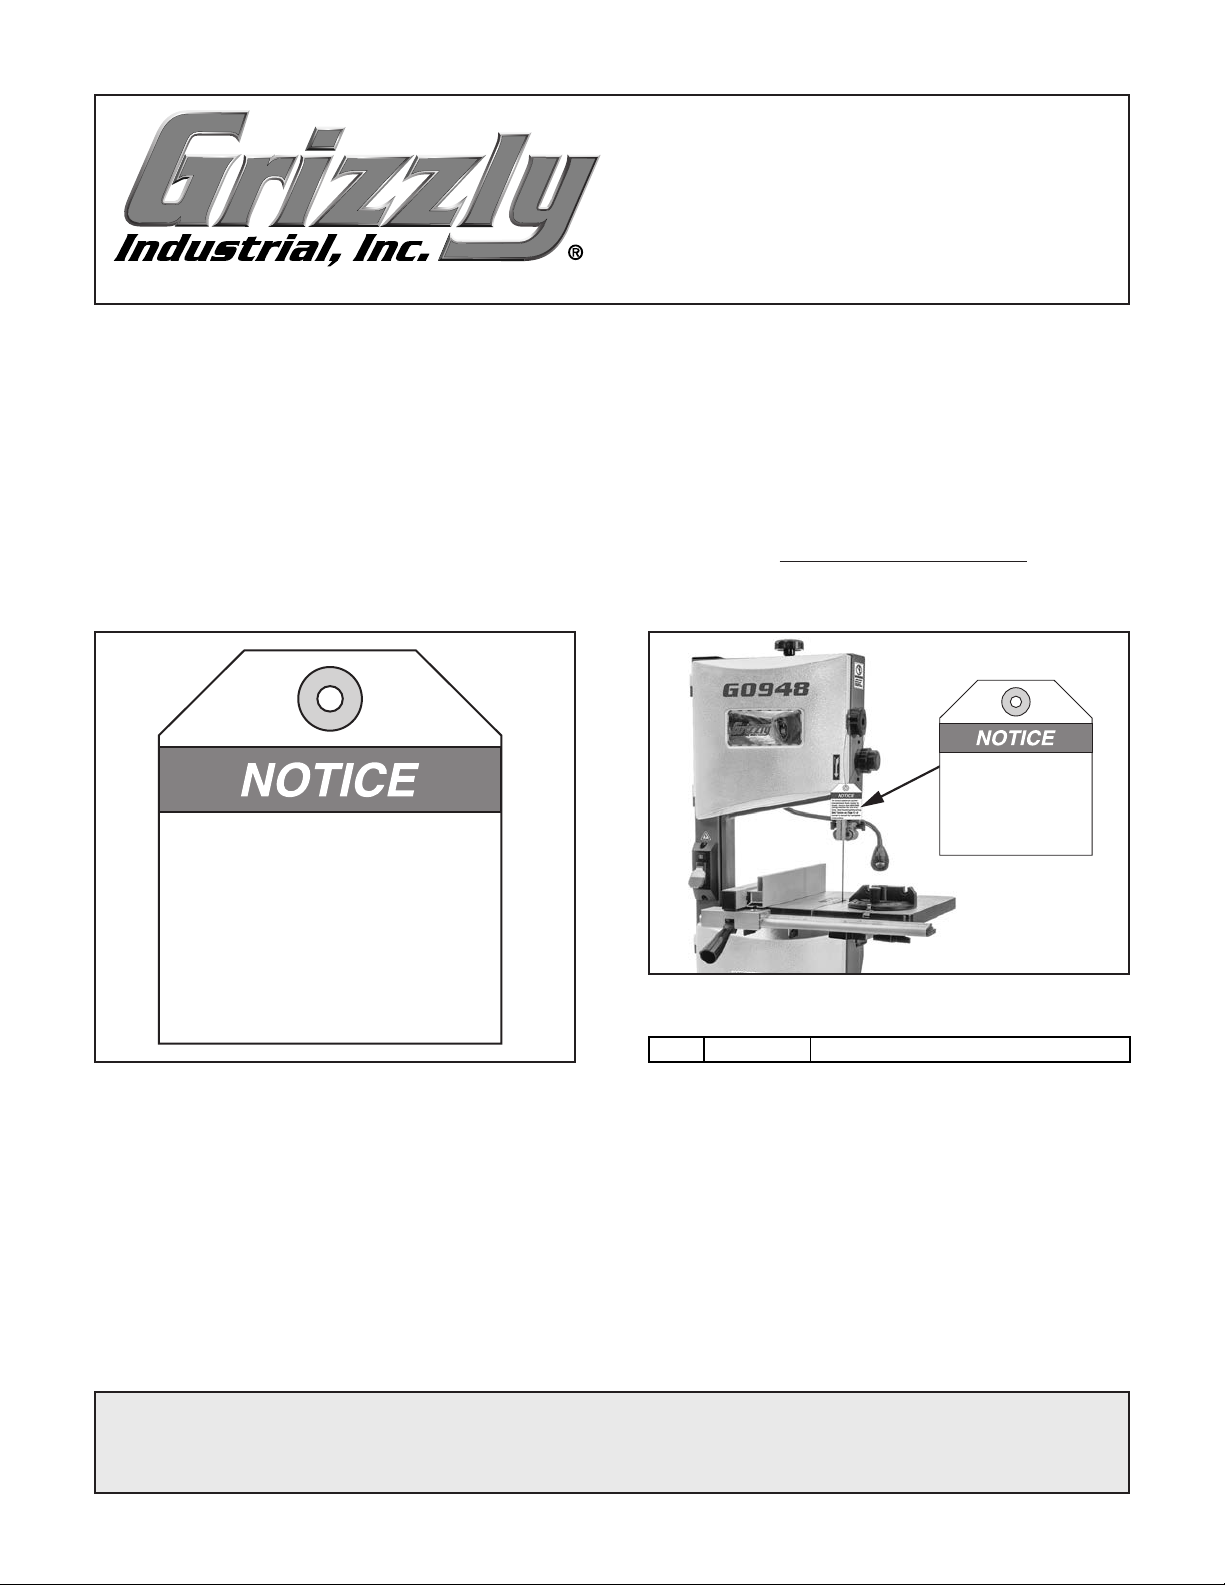
• New notice tag added advising users to properly tension belt before using machine for the first time.
Aside from this information, all other content in the owner's manual applies and MUST be read and understood for your own safety. IMPORTANT: Keep this update with the owner's manual for future reference.
For questions or help, contact our Tech Support at (570) 546-9663 or [email protected].
New Notice Tag
To ensure optimum power
transmission from motor to
blade, tension belt BEFORE
performing Test Run on Page
21. See Checking/Adjusting
Belt Tension on Page 51 of
owner’s manual for complete
instructions.
Revised Parts
To ensure optimum power
transmission from motor to
blade, tension belt BEFORE
performing Test Run on Page
21. See Checking/Adjusting
Belt Tension on Page 51 of
owner’s manual for complete
instructions.
212
REF PART # DES CRIPTI ON
212 P0948212 BELT TENSION NOTICE TAG
COPYRIGHT © SEPTEMBER, 2022 BY GRIZZLY INDUSTRIAL, INC.
WARNING: NO PORTION OF THIS MANUAL MAY BE REPRODUCED IN ANY SHAPE
OR FORM WITHOUT THE WRITTEN APPROVAL OF GRIZZLY INDUSTRIAL, INC.
#MN22474 PRINTED IN CHINA
Page 2
MODEL G0948
10" 1/2 HP BANDSAW
OWNER'S MANUAL
(For models manufactured since 08/21)
COPYRIGHT © SEPTEMBER, 2021 BY GRIZZLY INDUSTRIAL, INC.
WARNING: NO PORTION OF THIS MANUAL MAY BE REPRODUCED IN ANY SHAPE
OR FORM WITHOUT THE WRITTEN APPROVAL OF GRIZZLY INDUSTRIAL, INC.
#MN22059 PRINTED IN CHINA
V1.09.21
Page 3
This manual provides critical safety instructions on the proper setup,
operation, maintenance, and service of this machine/tool. Save this
document, refer to it often, and use it to instruct other operators.
Failure to read, understand and follow the instructions in this manual
may result in fire or serious personal injury—including amputation,
electrocution, or death.
The owner of this machine/tool is solely responsible for its safe use.
This responsibility includes but is not limited to proper installation in
a safe environment, personnel training and usage authorization,
proper inspection and maintenance, manual availability and comprehension, application of safety devices, cutting/sanding/grinding tool
integrity, and the usage of personal protective equipment.
The manufacturer will not be held liable for injury or property damage
from negligence, improper training, machine modifications or misuse.
Some dust created by power sanding, sawing, grinding, drilling, and
other construction activities contains chemicals known to the State
of California to cause cancer, birth defects or other reproductive
harm. Some examples of these chemicals are:
• Lead from lead-based paints.
• Crystalline silica from bricks, cement and other masonry products.
• Arsenic and chromium from chemically-treated lumber.
Your risk from these exposures varies, depending on how often you
do this type of work. To reduce your exposure to these chemicals:
Work in a well ventilated area, and work with approved safety equipment, such as those dust masks that are specially designed to filter
out microscopic particles.
Page 4
Table of Contents
INTRODUCTION ............................................... 2
Contact Info.................................................... 2
Manual Accuracy
Identification
Controls & Components
Machine Data Sheet
SECTION 1: SAFETY
Safety Instructions for Machinery
Additional Safety for Bandsaws
SECTION 2: POWER SUPPLY
SECTION 3: SETUP
Unpacking
Needed for Setup
Inventory
Hardware Recognition Chart
Site Considerations
Assembly
Dust Collection
Adjustment Overview
Initial Blade Tracking
Test Run
Tensioning Blade
Adjusting Blade Support Bearings
Adjusting Blade Guide Bearings
Aligning Table
Aligning Fence
Calibrating Miter Gauge
.................................................... 13
...................................................... 14
..................................................... 16
...................................................... 21
........................................... 2
................................................... 3
................................. 4
...................................... 6
....................................... 8
.................. 8
................... 10
...................... 11
....................................... 13
......................................... 13
....................... 15
...................................... 16
............................................. 19
................................... 19
................................... 20
......................................... 22
............... 24
.................. 25
.............................................. 27
............................................. 28
............................... 29
SECTION 5: ACCESSORIES
SECTION 6: MAINTENANCE
Schedule
Cleaning & Lubricating
SECTION 7: SERVICE
Troubleshooting
Checking/Adjusting Belt Tension
Replacing Belt
Aligning Wheels
Blade Lead
Adjusting Wheel Brush
SECTION 8: WIRING
Wiring Safety Instructions
Wiring Diagram
Electrical Components
SECTION 9: PARTS
Main
Labels & Cosmetics
WARRANTY & RETURNS
...................................................... 47
................................. 47
................................... 48
........................................... 48
.............................................. 52
........................................... 53
................................................... 56
................................ 57
...................................... 58
............................ 58
............................................ 59
................................. 60
....................................... 61
............................................................. 61
..................................... 64
............................. 65
......................... 44
......................... 47
................. 51
SECTION 4: OPERATIONS
Operation Overview
Basic Functions of a Bandsaw
Workpiece Inspection................................... 31
Setting Upper Blade Guide Height
Tilting Table
Choosing Blades
Blade Selection Chart
Blade Care & Break-In
Blade Breakage
Removing/Installing Blade
Changing Blade Speed
Ripping
Crosscutting
Resawing
Cutting Curves
Stacked Cuts................................................ 43
................................................. 32
.......................................... 34
........................................... 38
......................................................... 41
................................................. 41
..................................................... 42
............................................. 42
........................... 30
..................................... 30
.................... 31
.............. 32
.................................. 37
................................. 38
........................... 39
................................ 40
Page 5
We stand behind our machines! If you have questions or need help, contact us with the information
below. Before contacting, make sure you get the
serial number
from the
machine ID label. This will help us help you faster.
We want your feedback on this manual. What did
you like about it? Where could it be improved?
Please take a few minutes to give us feedback.
Email: [email protected]
We are proud to provide a high-quality owner’s
manual with your new machine!
We
instructions, specifications, drawings, and photographs
in this manual. Sometimes we make mistakes, but
our policy of continuous improvement also means
that
you receive is
slightly different than shown in the manual
If you find this to be the case, and the difference
between the manual and machine leaves you
confused or unsure about something
check our
website for an updated version. W
current
manuals and
on our web-
site at
Alternatively, you can call our Technical Support
for help. Before calling, make sure you write
down the
serial number
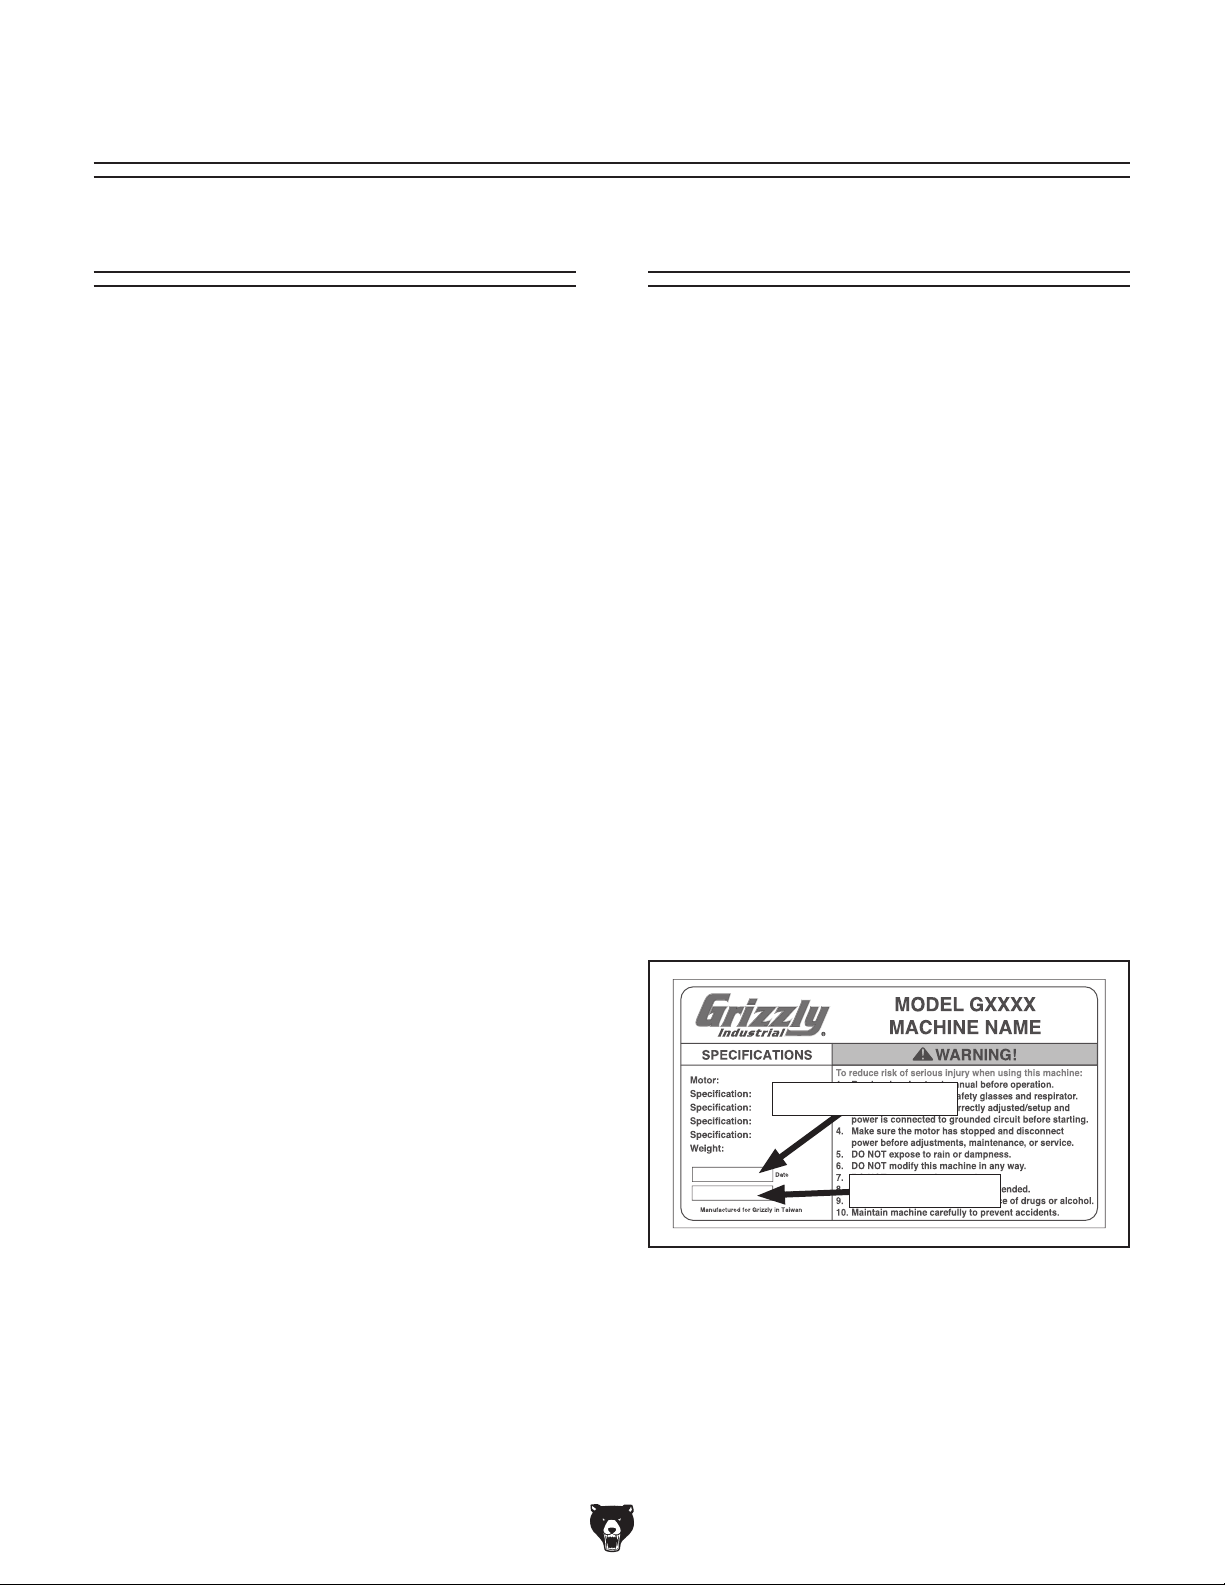
from the machine ID label (see below). This
information is required for us to provide proper
tech support, and it helps us determine if updated
documentation is available for your machine.
INTRODUCTION
Contact Info
and manufacture date
Grizzly Technical Support
1815 W. Battlefield
Springfield, MO 65807
Phone: (570) 546-9663
Email: [email protected]
Grizzly Documentation Manager
P.O. Box 2069
Bellingham, WA 98227-2069
Manual Accuracy
made every effort to be exact with the
sometimes the machine
.
,
e post
manual updates for free
www.grizzly.com.
manufacture date and
Manufacture Date
Serial Number
-2-
Model G0948 (Mfd. Since 08/21)
Page 6
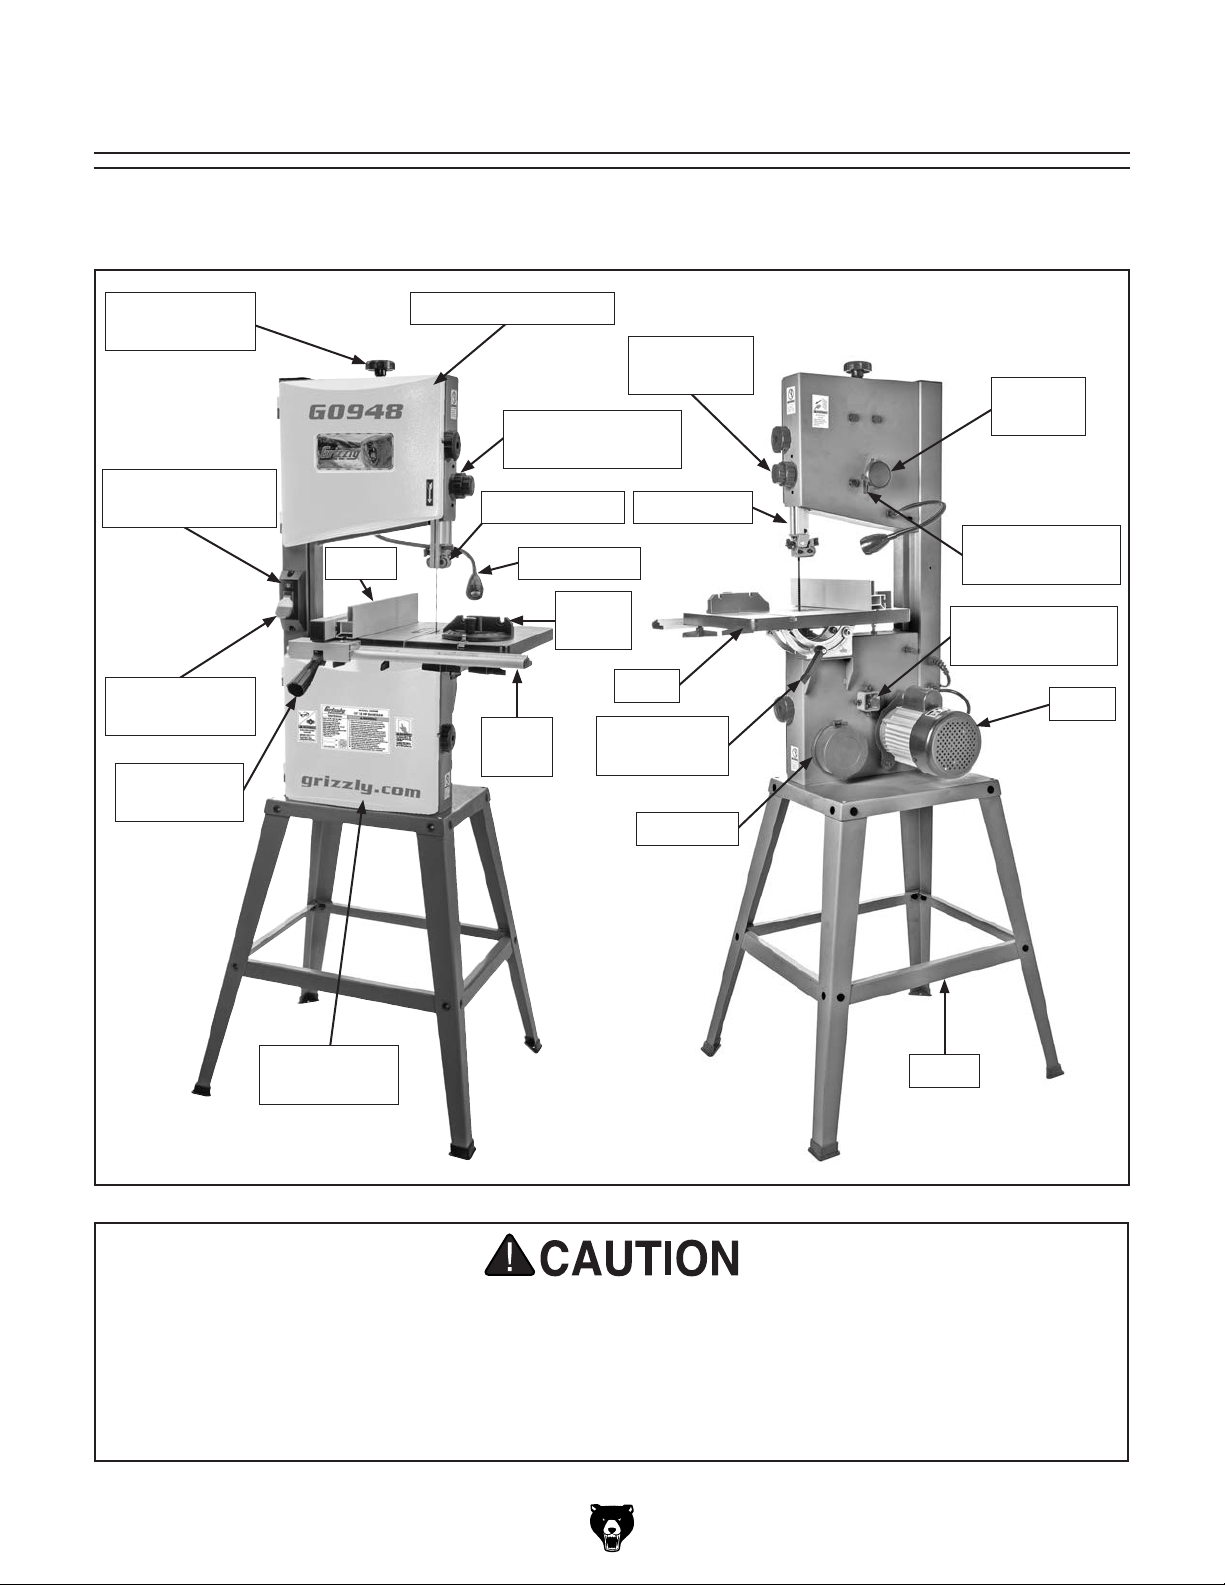
Identification
Become familiar with the names and locations of the controls and features shown below to better understand
the instructions in this manual.
Upper Wheel CoverBlade Tension
Knob
LED Work Light
ON/OFF Switch
Fence
Guide Post
Adjustment Knob
Blade Guides
Work Light
Guide Post
Lock Knob
Guide Post
Tracking
Knob
Tracking Knob
Lock Lever
ON/OFF
Paddle Switch
Fence Lock
Handle
Lower Wheel
Cover
Fence
Rail
Miter
Gauge
Table
Table Tilt
Lock Handle
Lower Wheel
Adjustment Hub
Motor
Dust Port
Stand
For Your Own Safety, Read Instruction Manual Before Operating Saw.
a) Wear eye protection.
b) Do not remove jammed cutoff pieces until blade has stopped.
c) Maintain proper adjustment of blade tension, blade guides, and thrust bearings.
d) Adjust upper blade guide to just clear workpiece.
e) Hold workpiece firmly against table.
Model G0948 (Mfd. Since 08/21)
-3-
Page 7
Controls &
To reduce your risk of
serious injury, read this
entire manual BEFORE
Components
Fence & Miter Gauge
using machine.
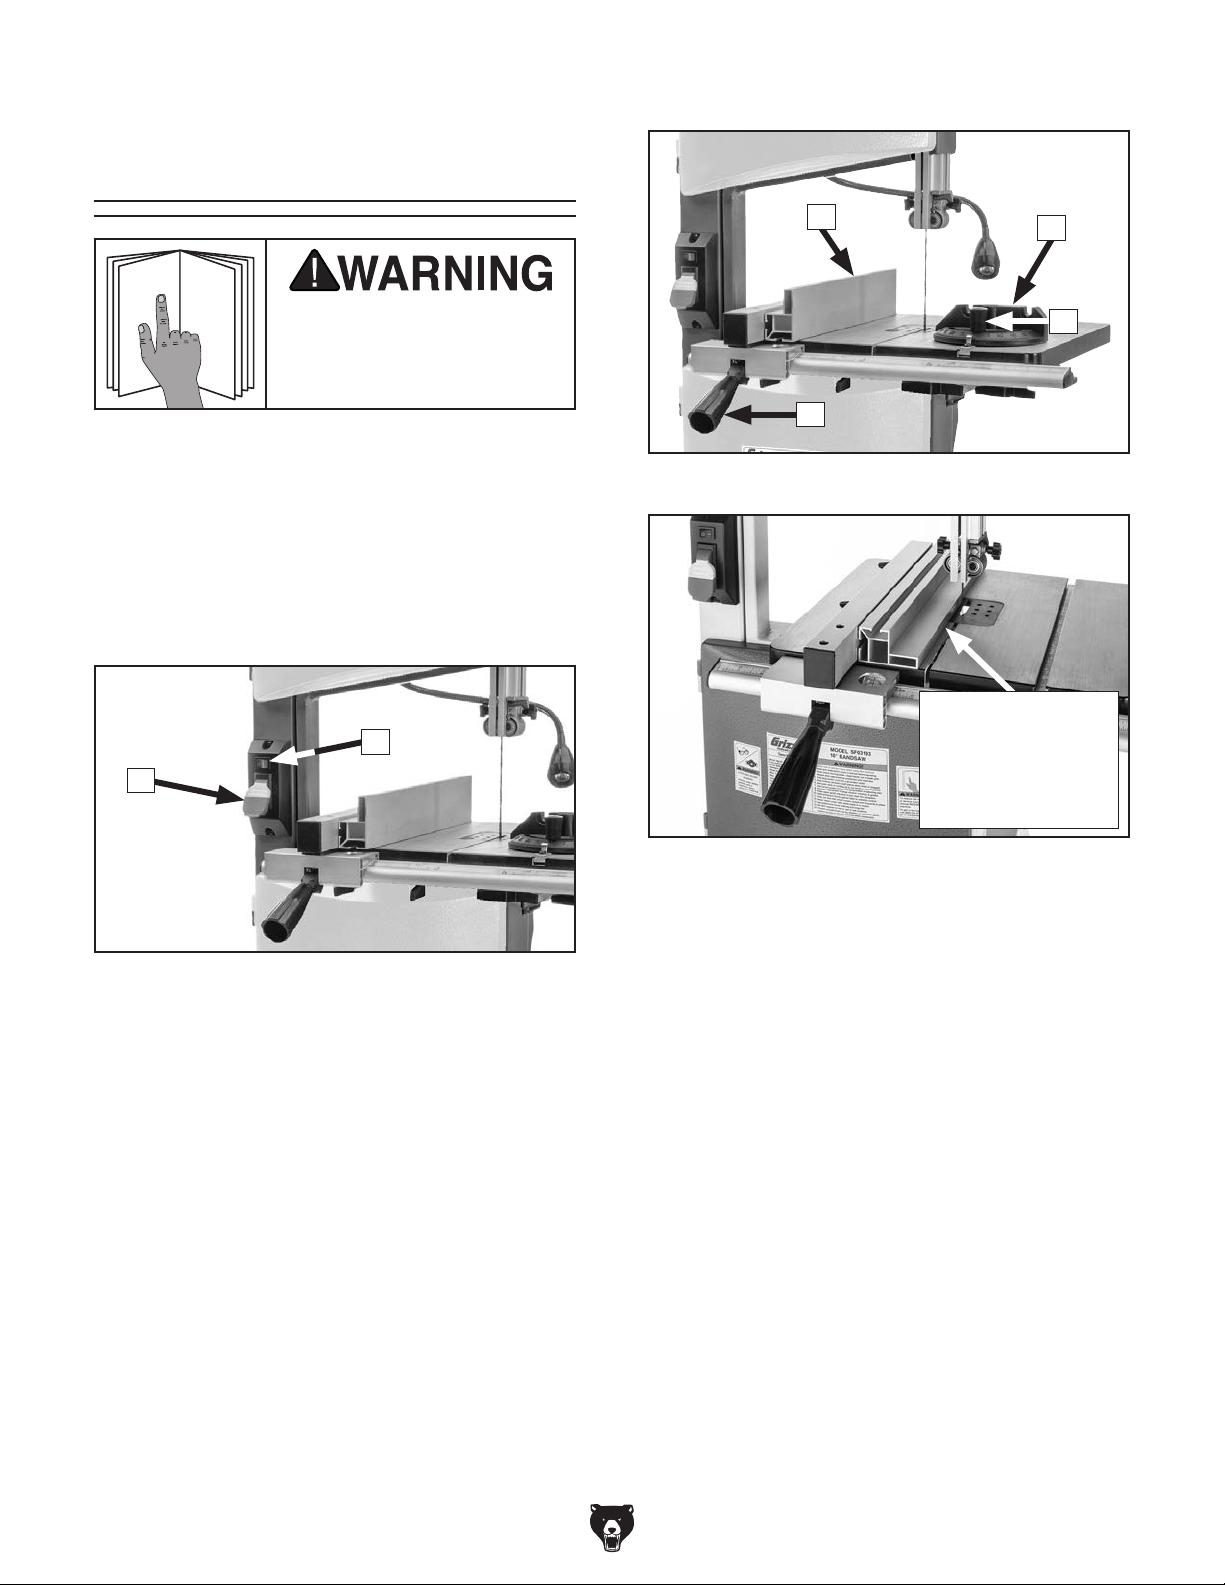
Refer to Figures 1–6 and the following descriptions to become familiar with the basic controls
and components of this machine. Understanding
these items and how they work will help you
understand the rest of the manual and stay safe
when operating this machine.
Power Controls
B
A
C
F
Figure 2. Fence and miter gauge controls.
Horizontal Position
Allows Upper
Blade Guide to Be
Adjusted Closer to
Thin Workpieces
D
E
Figure 1. Power controls.
A. ON/OFF Paddle Switch w/Removable Key:
Turns machine ON and OFF. Remove key to
disable machine.
LED Work Light ON/OFF Switch: Turns
B.
light ON and OFF. Illuminates cutting area for
better visibility.
Figure 3. Fence mounted in horizontal position.
C. Fence: Used for ripping or resawing. Distance
from blade determines width of cut. Can be
used in vertical position (as shown in Figure
2) for normal workpieces, or in horizontal
position (as shown in Figure 3) for thin
workpieces.
D. Miter Gauge: Typically used for cross cuts.
Can be adjusted from 0°–60° left or right.
E. Miter Gauge Lock Knob: Secures angle
position of miter gauge.
F. Fence Lock Handle: Secures fence position.
-4-
Model G0948 (Mfd. Since 08/21)
Page 8
Guide Post
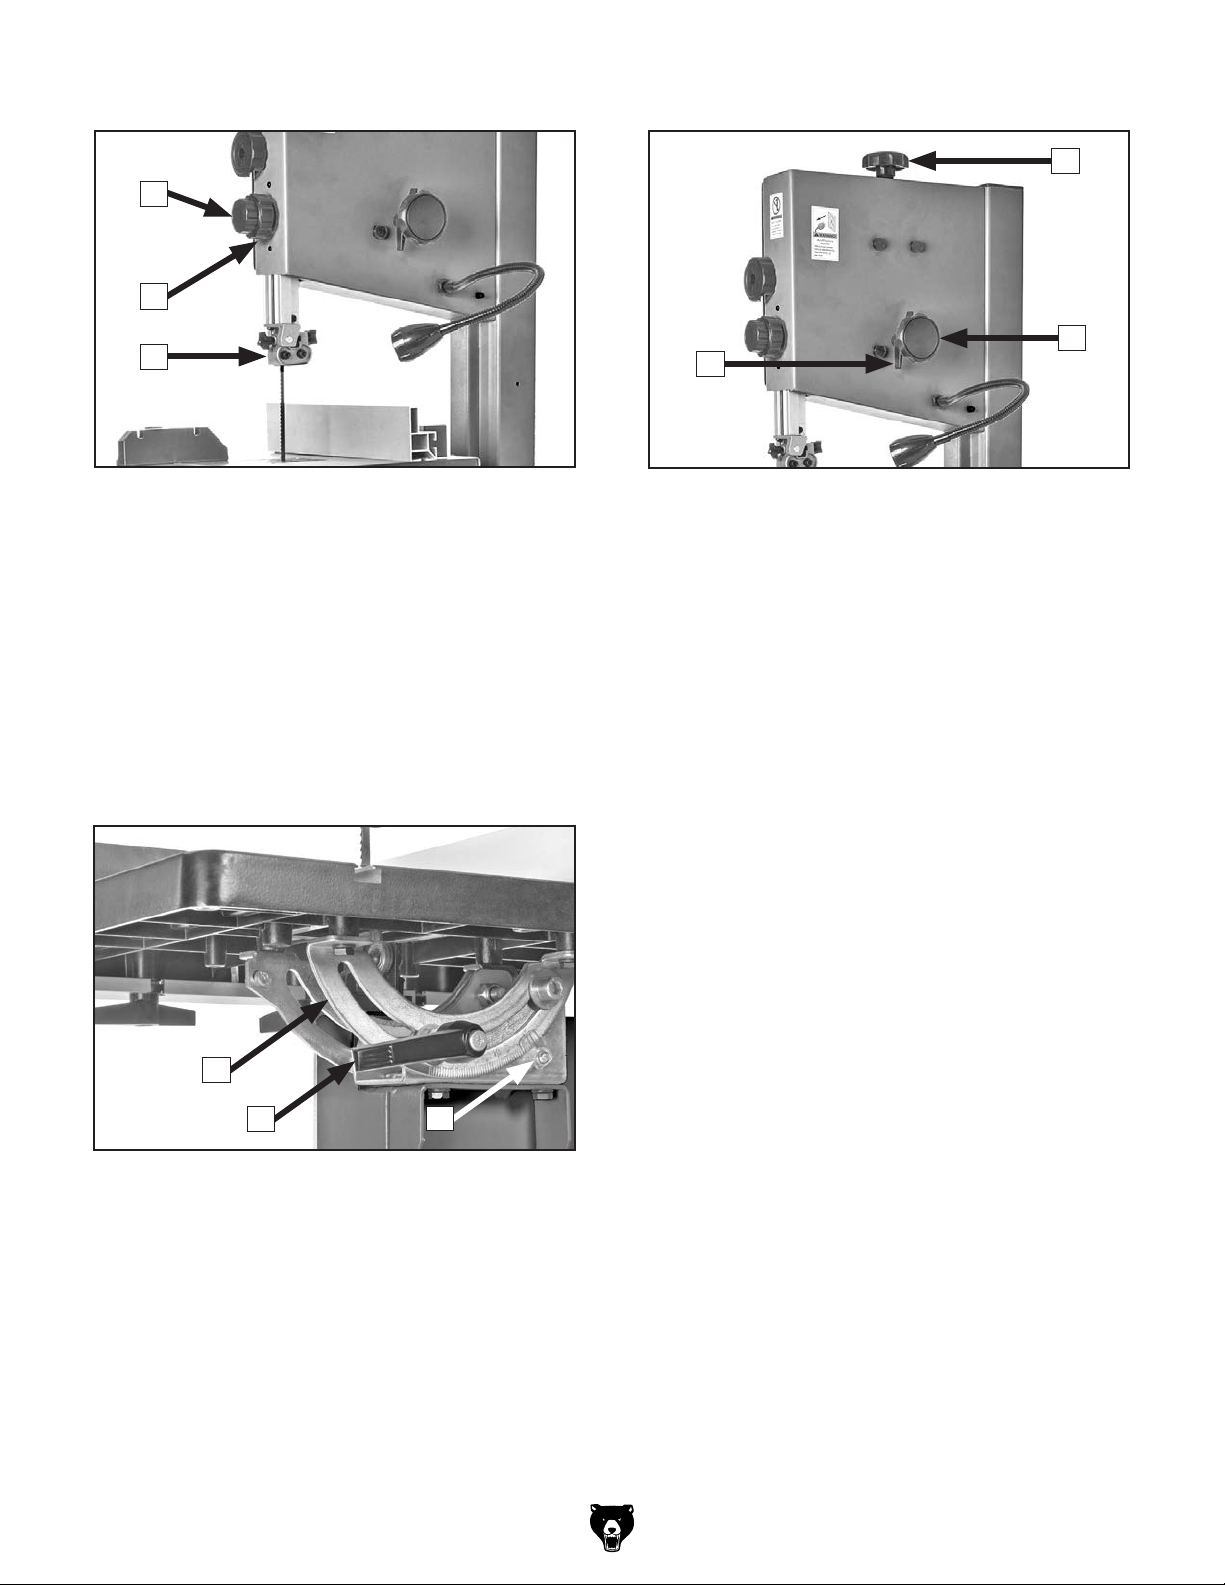
G
H
Blade Tension & Tracking
M
I
Figure 4. Guide post controls.
G. Guide Post Lock Knob: Secures height of
blade guides.
H. Guide Post Adjustment Knob: Rotate
to adjust height of blade guides above
workpiece.
I. Upper Blade Guide: Supports blade above
workpiece during operations.
Table Tilt
N
O
Figure 6. Blade tension and tracking controls.
M. Blade Tension Adjustment Knob: Rotate
to adjust blade tension (refer to
more information).
Blade Tracking Knob: Rotate to adjust
N.
blade tracking (refer to Page 20 for more
information).
O. Blade Tracking Knob Lock Lever: Secures
position of tracking knob.
Page 22 for
J
K
Figure 5. Table tilt controls.
J. Trunnion w/Table Tilt Scale: Functions as
a tilting base for table. Graduated in degrees
from 0°–45° for setting bevel angle.
Table Tilt Lock Lever: Secures table tilt
K.
angle setting.
L. Table Tilt Indicator: Shows angle of table
tilt.
Model G0948 (Mfd. Since 08/21)
L
-5-
Page 9
MACHINE DATA
Has Quick-Release........................................................................................................................................ No
SHEET
Customer Service #: (570) 546-9663 · To Order Call: (800) 523-4777 · Fax #: (800) 438-5901
MODEL G0948 10" 1/2 HP BANDSAW
Product Dimensions:
Weight................................................................................................................................................................ 69 lbs.
Width (side-to-side) x Depth (front-to-back) x Height............................................................... 28 x 21-1/2 x 58-1/2 in.
Footprint (Length x Width)............................................................................................................... 24-1/2 x 20-1/2 in.
Shipping Dimensions:
Type............................................................................................................................................................. Cardboard
Content........................................................................................................................................................... Machine
Weight................................................................................................................................................................ 75 lbs.
Length x Width x Height....................................................................................................................... 38 x 19 x 16 in.
Must Ship Upright.................................................................................................................................................... No
Electrical:
Power Requirement........................................................................................................... 120V, Single-Phase, 60 Hz
Full-Load Current Rating....................................................................................................................................... 3.5A
Minimum Circuit Size.............................................................................................................................................. 15A
Connection Type....................................................................................................................................... Cord & Plug
Power Cord Included.............................................................................................................................................. Yes
Power Cord Length.............................................................................................................................................. 72 in.
Power Cord Gauge......................................................................................................................................... 18 AWG
Plug Included.......................................................................................................................................................... Yes
Included Plug Type................................................................................................................................................ 5-15
Switch Type.................................................................................................. Paddle Safety Switch w/Removable Key
Motors:
Main
Horsepower............................................................................................................................................. 1/2 HP
Phase............................................................................................................................................ Single-Phase
Amps........................................................................................................................................................... 3.5A
Speed................................................................................................................................................ 1720 RPM
Type................................................................................................................. TEFC Capacitor-Start Induction
Power Transfer ............................................................................................................................................ Belt
Bearings..................................................................................................... Shielded & Permanently Lubricated
Main Specifications:
Main Specifications
Bandsaw Size............................................................................................................................................ 10 in.
Max Cutting Width (Left of Blade).......................................................................................................... 9-3/4 in.
Max Cutting Width (Left of Blade) w/Fence........................................................................................... 6-1/8 in.
Max Cutting Height (Resaw Height)...................................................................................................... 6-1/8 in.
Blade Speeds........................................................................................................................... 1520, 2620 FPM
Blade Information
Standard Blade Length.............................................................................................................................. 72 in.
Blade Length Range.............................................................................................................. 71-1/2 - 72-1/2 in.
Blade Width Range........................................................................................................................... 1/8 - 1/2 in.
Type of Blade Guides...................................................................................................................... Ball Bearing
Guide Post Adjustment Type....................................................................................................... Rack & Pinion
-6-
Model G0948 (Mfd. Since 08/21)
Page 10
Table Information
Table Length...................................................................................................................................... 14-3/16 in.
Table Width......................................................................................................................................... 12-5/8 in.
Table Thickness........................................................................................................................................... 1 in.
Table Tilt............................................................................................................................................ 0 - 45 deg.
Table Tilt Adjustment Type..................................................................................................................... Manual
Floor-to-Table Height........................................................................................................................... 38-5/8 in.
Fence Locking Position.............................................................................................................................. Front
Fence is Adjustable for Blade Lead.............................................................................................................. Yes
Resaw Fence Attachment Included.............................................................................................................. Yes
Miter Gauge Included................................................................................................................................... Yes
Construction Materials
Table.......................................................................................................................................... Cast Aluminum
Trunnion..................................................................................................................................................... Steel
Fence.................................................................................................................................................. Aluminum
Base/Stand................................................................................................................................................. Steel
Frame/Body................................................................................................................................................ Steel
Wheels....................................................................................................................................... Cast Aluminum
Tire.......................................................................................................................................................... Rubber
Wheel Cover .............................................................................................................................................. Steel
Paint Type/Finish................................................................................................................................. Urethane
Other Related Information
Wheel Diameter......................................................................................................................................... 10 in.
Wheel Width............................................................................................................................................. 1/2 in.
Number of Dust Ports....................................................................................................................................... 1
Dust Port Size...................................................................................................................................... 2, 3, 4 in.
Other Specifications:
Country of Origin ................................................................................................................................................ China
Warranty ........................................................................................................................................................... 1 Year
Approximate Assembly & Setup Time ........................................................................................................ 30 Minutes
Serial Number Location ................................................................................................................... Machine ID Label
ISO 9001 Factory .................................................................................................................................................. Yes
Features:
Steel Stand w/Vibration-Resistant Rubber Feet
Ball-Bearing Blade Guides
LED Work Light
Extruded Aluminum Rip Fence
Combination 2", 3" & 4" Dust Port
45-Degree Table Tilt
6-1/8" Cutting Height (Resaw Capacity)
Blade Speeds: 1520, 2620 FPM
Accessories Included:
Push Stick
Miter Gauge
Open-Ends Wrench 10/13mm
Hex Wrenches 3, 4, 5, 6mm
Model G0948 (Mfd. Since 08/21)
-7-
Page 11
SECTION 1: SAFETY
For Your Own Safety, Read Instruction
Manual Before Operating This Machine
The purpose of safety symbols is to attract your attention to possible hazardous conditions.
This manual uses a series of symbols and signal words intended to convey the level of importance of the safety messages. The progression of symbols is described below. Remember that
safety messages by themselves do not eliminate danger and are not a substitute for proper
accident prevention measures. Always use common sense and good judgment.
Indicates an imminently hazardous situation which, if not avoided,
WILL result in death or serious injury.
Indicates a potentially hazardous situation which, if not avoided,
COULD result in death or serious injury.
Indicates a potentially hazardous situation which, if not avoided,
MAY result in minor or moderate injury. It may also be used to alert
against unsafe practices.
Alerts the user to useful information about proper operation of the
NOTICE
machine to avoid machine damage.
Safety Instructions for Machinery
OWNER’S MANUAL. Read and understand this
owner’s manual BEFORE using machine.
TRAINED OPERATORS ONLY. Untrained operators have a higher risk of being hurt or killed.
Only allow trained/supervised people to use this
machine. When machine is not being used, disconnect power, remove switch keys, or lock-out
machine to prevent unauthorized use—especially
around children. Make your workshop kid proof!
DANGEROUS ENVIRONMENTS. Do not use
machinery in areas that are wet, cluttered, or have
poor lighting. Operating machinery in these areas
greatly increases the risk of accidents and injury.
MENTAL ALERTNESS REQUIRED. Full mental
alertness is required for safe operation of machinery. Never operate under the influence of drugs or
alcohol, when tired, or when distracted.
ELECTRICAL EQUIPMENT INJURY RISKS.
You can be shocked, burned, or killed by touching
live electrical components or improperly grounded
machinery. To reduce this risk, only allow qualified
service personnel to do electrical installation or
repair work, and always disconnect power before
accessing or exposing electrical equipment.
DISCONNECT POWER FIRST.
nect machine from power supply BEFORE making adjustments, changing tooling, or servicing
machine. This prevents an injury risk from unintended startup or contact with live electrical components.
EYE PROTECTION. Always wear ANSI-approved
safety glasses or a face shield when operating or
observing machinery to reduce the risk of eye
injury or blindness from flying particles. Everyday
eyeglasses are NOT approved safety glasses.
Always discon-
-8-
Model G0948 (Mfd. Since 08/21)
Page 12
WEARING PROPER APPAREL. Do not wear
clothing, apparel or jewelry that can become
entangled in moving parts. Always tie back or
cover long hair. Wear non-slip footwear to reduce
risk of slipping and losing control or accidentally
contacting cutting tool or moving parts.
HAZARDOUS DUST. Dust created by machinery
operations may cause cancer, birth defects, or
long-term respiratory damage. Be aware of dust
hazards associated with each workpiece material. Always wear a NIOSH-approved respirator to
reduce your risk.
HEARING PROTECTION. Always wear hearing protection when operating or observing loud
machinery. Extended exposure to this noise
without hearing protection can cause permanent
hearing loss.
REMOVE ADJUSTING TOOLS. Tools left on
machinery can become dangerous projectiles
upon startup. Never leave chuck keys, wrenches,
or any other tools on machine. Always verify
removal before starting!
USE CORRECT TOOL FOR THE JOB. Only use
this tool for its intended purpose—do not force
it or an attachment to do a job for which it was
not designed. Never make unapproved modifications—modifying tool or using it differently than
intended may result in malfunction or mechanical
failure that can lead to personal injury or death!
AWKWARD POSITIONS. Keep proper footing
and balance at all times when operating machine.
Do not overreach! Avoid awkward hand positions
that make workpiece control difficult or increase
the risk of accidental injury.
CHILDREN & BYSTANDERS. Keep children and
bystanders at a safe distance from the work area.
Stop using machine if they become a distraction.
GUARDS & COVERS. Guards and covers reduce
accidental contact with moving parts or flying
debris. Make sure they are properly installed,
undamaged, and working correctly BEFORE
operating machine.
FORCING MACHINERY. Do not force machine.
It will do the job safer and better at the rate for
which it was designed.
NEVER STAND ON MACHINE. Serious injury
may occur if machine is tipped or if the cutting
tool is unintentionally contacted.
STABLE MACHINE. Unexpected movement during operation greatly increases risk of injury or
loss of control. Before starting, verify machine is
stable and mobile base (if used) is locked.
USE RECOMMENDED ACCESSORIES. Consult
this owner’s manual or the manufacturer for recommended accessories. Using improper accessories will increase the risk of serious injury.
UNATTENDED OPERATION. To reduce the
risk of accidental injury, turn machine OFF and
ensure all moving parts completely stop before
walking away. Never leave machine running
while unattended.
MAINTAIN WITH CARE. Follow all maintenance
instructions and lubrication schedules to keep
machine in good working condition. A machine
that is improperly maintained could malfunction,
leading to serious personal injury or death.
DAMAGED PARTS. Regularly inspect machine
for damaged, loose, or mis-adjusted parts—or
any condition that could affect safe operation.
Immediately repair/replace BEFORE operating
machine. For your own safety, DO NOT operate
machine with damaged parts!
MAINTAIN POWER CORDS. When disconnecting cord-connected machines from power, grab
and pull the plug—NOT the cord. Pulling the cord
may damage the wires inside. Do not handle
cord/plug with wet hands. Avoid cord damage by
keeping it away from heated surfaces, high traffic
areas, harsh chemicals, and wet/damp locations.
EXPERIENCING DIFFICULTIES. If at any time
you experience difficulties performing the intended operation, stop using the machine! Contact our
Technical Support at (570) 546-9663.
Model G0948 (Mfd. Since 08/21)
-9-
Page 13
Additional Safety for Bandsaws
Serious cuts, amputation, or death can occur from contact with the moving saw blade during
operation or if blade breakage occurs. Serious injury or death can also occur from getting
fingers, hair, or clothing entangled in moving parts if the machine is operated while the doors
are open. To reduce this risk, anyone operating this machine MUST completely heed the
hazards and warnings below.
HAND PLACEMENT. Placing hands or fingers
in line with blade during operation may result in
serious injury if hands slip or workpiece moves
unexpectedly. Do not position fingers or hands in
line with blade, and never reach under table while
blade is moving.
SMALL/NARROW WORKPIECES. If hands slip
during a cut while holding small workpieces with
fingers, serious personal injury could occur. Always
support/feed small or narrow workpieces with push
sticks, push blocks, jig, vise, clamping fixture.
BLADE SPEED. Cutting workpiece before blade
is at full speed could cause blade to grab workpiece and pull hands into blade. Allow blade to
reach full speed before starting cut. DO NOT start
machine with workpiece contacting blade.
FEED RATE. To avoid risk of workpiece slipping
and causing operator injury, always feed stock
evenly and smoothly.
BLADE CONDITION. Dull blades require more
effort to perform cut, increasing risk of accidents.
Do not operate with dirt y, dull, cracked or badly
worn blades. Inspect blades for cracks and missing teeth before each use. Always maintain proper
blade tension and tracking while operating.
CLEARING JAMS AND CUTOFFS. Always stop
bandsaw and disconnect power before clearing
scrap pieces that get stuck between blade and
table insert. Use brush or push stick, not hands,
to clean chips/cutoff scraps from table.
BLADE CONTROL. To avoid risk of injury due to
blade contact, always allow blade to stop on its
own. DO NOT try to stop or slow blade with your
hand or the workpiece.
GUARDS /COVERS. Blade guards and covers
protect operator from moving bandsaw blade. The
wheel covers protect operator from getting entangled with rotating wheels or other moving parts.
ON LY operate bandsaw with blade guard in proper
position and wheel covers completely closed.
BLADE REPLACEMENT. To avoid mishaps that
could result in operator injury, make sure blade
teeth face down toward table and blade is properly tensioned and tracked before operating.
UPPER BLADE GUIDE SUPPORT. To reduce
exposure of operator to blade and provide maximum blade support while cutting, keep upper
blade guides adjusted to just clear workpiece.
CUTTING TECHNIQUES. To avoid blade getting
pulled off wheels or accidentally breaking and
striking operator, always turn bandsaw OFF and
wait for blade to come to a complete stop before
backing workpiece out of blade. DO NOT back
workpiece away from blade while bandsaw is running. DO NOT force or twist blade while cutting,
especially when sawing small curves. This could
result in blade damage or breakage.
WORKPIECE SUPPORT. To maintain maximum
control and reduce risk of blade contact/breakage, always ensure adequate support of long/
large workpieces. Always keep workpiece flat and
firm against table/fence when cutting to avoid loss
of control. If necessary, use a jig or other workholding device.
WORKPIECE MATERIAL. This machine is
intended for cutting natural and man-made wood
products, and laminate covered wood products.
This machine is NOT designed to cut metal,
glass, stone, tile, etc.
-10 -
Model G0948 (Mfd. Since 08/21)
Page 14
SECTION 2: POWER SUPPLY
Before installing the machine, consider the availability and proximity of the required power supply
circuit. If an existing circuit does not meet the
requirements for this machine, a new circuit must
be installed. To minimize the risk of electrocution,
fire, or equipment damage, installation work and
electrical wiring must be done by an electrician or
qualified service personnel in accordance with all
applicable codes and standards.
or equipment damage
not properly grounded
The full-load current rating is the amperage a
machine draws at 100% of the rated output power.
On machines with multiple motors, this is the
amperage drawn by the largest motor or sum of all
motors and electrical devices that might operate
at one time during normal operations.
The full-load current is not the maximum amount
of amps that the machine will draw. If the machine
is overloaded, it will draw additional amps beyond
the full-load rating.
If the machine is overloaded for a sufficient length
of time, damage, overheating, or fire may result—
especially if connected to an undersized circuit.
To reduce the risk of these hazards, avoid overloading the machine during operation and make
sure it is connected to a power supply circuit that
meets the specified circuit requirements.
For your own safety and protection of
Note: Circuit requirements in this manual apply to
a dedicated circuit—where only one machine will
be running on the circuit at a time. If machine will
be connected to a shared circuit where multiple
machines may be running at the same time, consult an electrician or qualified service personnel to
ensure circuit is properly sized for safe operation.
A power supply circuit includes all electrical
equipment between the breaker box or fuse panel
in the building and the machine. The power supply circuit used for this machine must be sized to
safely handle the full-load current drawn from the
machine for an extended period of time. (If this
machine is connected to a circuit protected by
fuses, use a time delay fuse marked D.)
This machine is prewired to operate on a power
supply circuit that has a verified ground and meets
the following requirements:
process. DO NOT connect to power until
Availability
Electrocution, fire, shock,
may occur if machine is
and connected to power
supply.
Serious injury could occur if you connect
machine to power before completing setup
instructed later in this manual.
120V Circuit Requirements
Nominal Voltage .................... 110V, 115 V, 12 0V
..........................................................60 Hz
Cycle
Phase
Power Supply Circuit
........................................... Single-Phase
......................... 15 Amps
Full-Load Current Rating
Full-Load Current Rating at 120V .... 3.5 Amps
Model G0948 (Mfd. Since 08/21)
property, consult an electrician if you are
unsure about wiring practices or electrical
codes in your area.
-11-
Page 15
Improper connection of the equipment-grounding
wire can result in a risk of electric shock. The
wire with green insulation (with or without yellow
stripes) is the equipment-grounding wire. If repair
or replacement of the power cord or plug is necessary, do not connect the equipment-grounding
wire to a live (current carrying) terminal.
Check with a qualified electrician or service personnel if you do not understand these grounding
requirements, or if you are in doubt about whether
the tool is properly grounded. If you ever notice
that a cord or plug is damaged or worn, disconnect it from power, and immediately replace it with
a new one.
We do not recommend using an extension cord
with this machine.
cord, only use it if absolutely necessary and only
on a temporary basis.
Extension cords cause voltage drop, which can
damage electrical components and shorten motor
life. Voltage drop increases as the extension cord
size gets longer and the gauge size gets smaller
(higher gauge numbers indicate smaller sizes).
Any extension cord used with this machine must
be in good condition and contain a ground wire
and matching plug/receptacle. Additionally, it must
meet the following size requirements:
Grounding & Plug Requirements
it will not fit the outlet, have a qualified
electrician install the proper outlet with a
This machine MUST be grounded. In the event
of certain malfunctions or breakdowns, grounding
reduces the risk of electric shock by providing a
path of least resistance for electric current.
This machine is equipped with a power cord that
has an equipment-grounding wire and a grounding
plug. Only insert plug into a matching receptacle
(outlet) that is properly installed and grounded in
accordance with all local codes and ordinances.
DO NOT modify the provided plug!
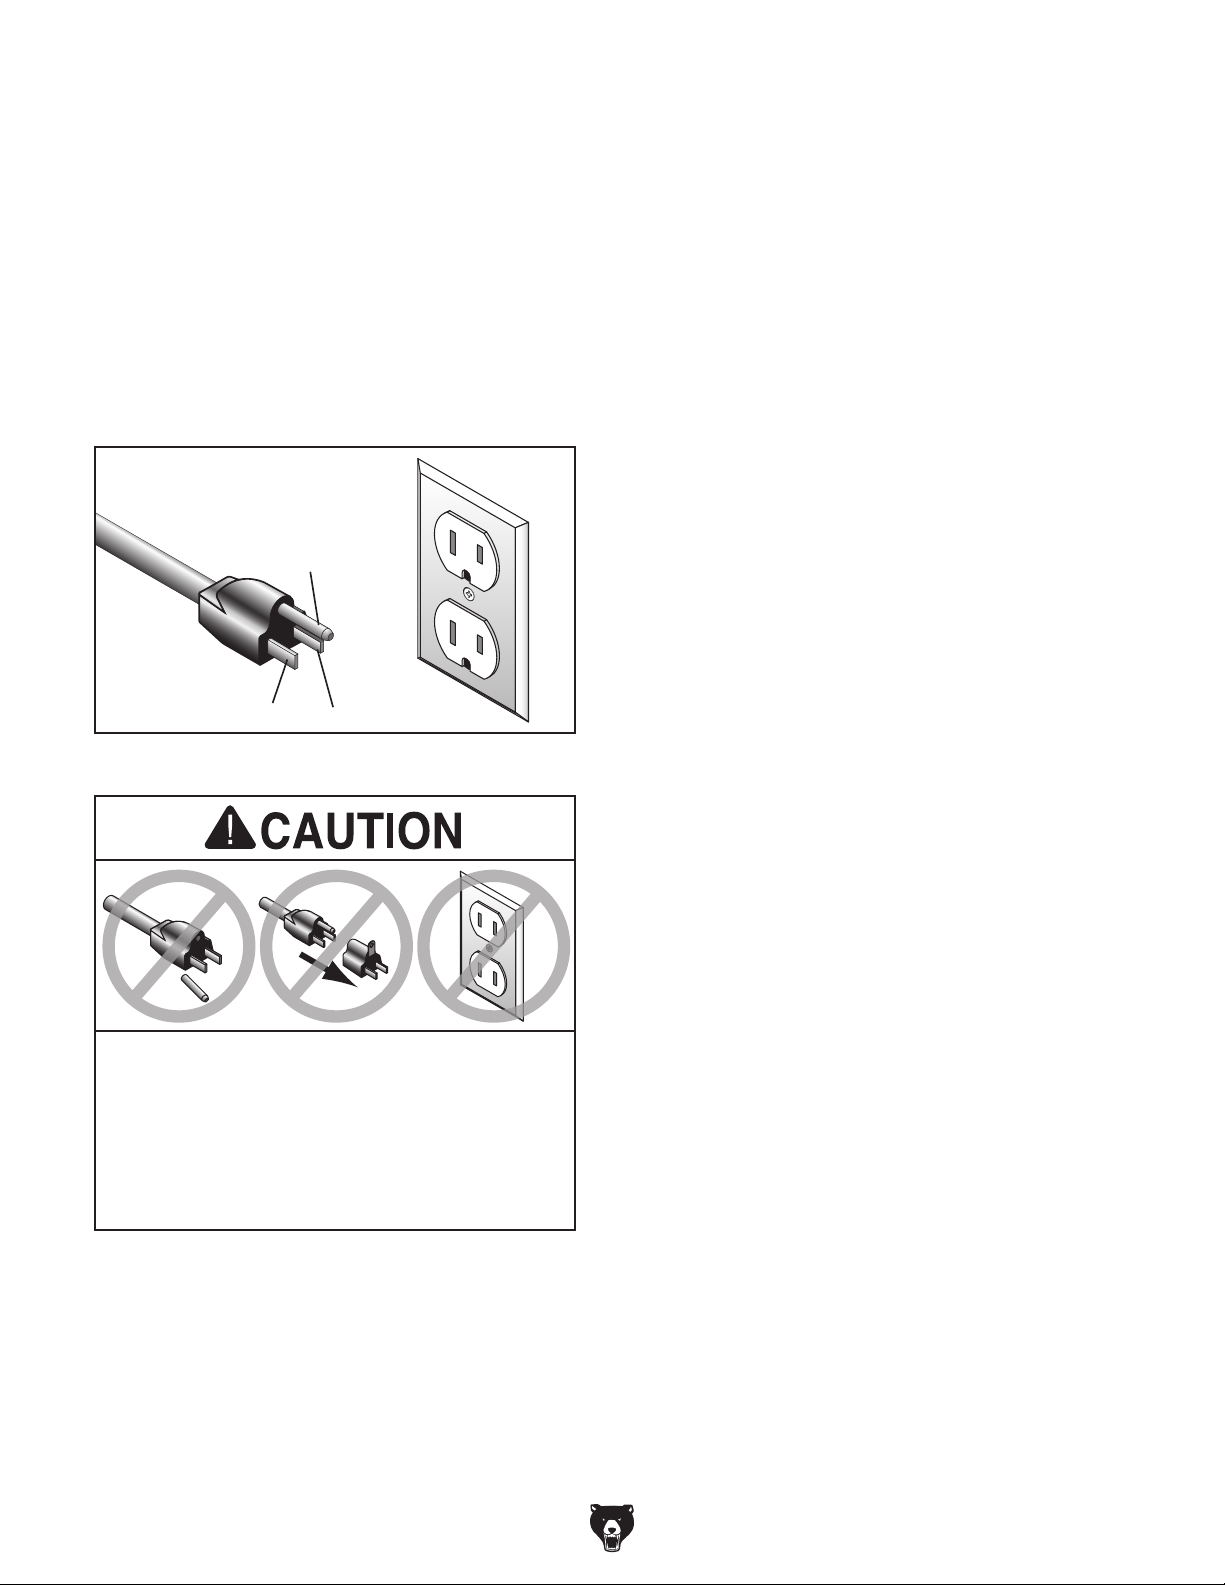
GROUNDED
5-15 RECEPTACLE
Grounding Pin
5-15 PLUG
Extension Cords
If you must use an extension
Neutral Hot
Figure 7. Typical 5-15 plug and receptacle.
SHOCK HAZARD!
Two-prong outlets do not meet the grounding
requirements for this machine. Do not modify
or use an adapter on the plug provided—if
verified ground.
-12-
Minimum Gauge Size ...........................16 AWG
Maximum Length (Shorter is Better).......50 ft.
Model G0948 (Mfd. Since 08/21)
Page 16
SECTION 3: SETUP
This machine was carefully packaged for safe
transport. When unpacking, separate all enclosed
items from packaging materials and inspect them
for shipping damage.
,
please
IMPORTANT:
you are completely satisfied with the machine and
have resolved any issues between Grizzly or the
shipping agent. You MUST have the original pack-
aging to file a freight claim. It is also extremely
helpful if you need to return your machine later.
This machine presents
serious injury hazards
to untrained users. Read
through this entire manual to become familiar with
the controls and operations before starting the
machine!
Wear safety glasses during
the entire setup process!
call us immediately at (570) 546-9663.
Unpacking
If items are damaged
Save all packaging materials until
Like all machinery there is potential danger
when operating this machine. Accidents are
frequently caused by lack of familiarity or
failure to pay attention. Use this machine
with respect and caution to decrease the
risk of operator injury. If normal safety precautions are overlooked or ignored, serious
personal injury may occur.
No list of safety guidelines can be complete.
Every shop environment is different. Always
consider safety first, as it applies to your
individual working conditions. Use this and
other machinery with caution and respect.
Failure to do so could result in serious personal injury, damage to equipment, or poor
work results.
Needed for Setup
The following items are needed, but not included,
for the setup/assembly of this machine.
Description Qty
• Additional Person ....................................... 1
• Safety Glasses (for each person) ............... 1
• Heavy Leather Gloves ........................... 1 Pr.
• Phillip's Head Screwdriver #2 ..................... 1
• Feeler Gauge 0.016" .................................. 1
• Straightedge ............................................... 1
• Ruler ........................................................... 1
• Shims ......................................... As Needed
• Machinist's Square ..................................... 1
• Level 18" ..................................................... 1
• Dust-Collection System .............................. 1
• Dust Hose 2", 3", or 4" ................................ 1
• Hose Clamps 2", 3", or 4" ........................... 2
Model G0948 (Mfd. Since 08/21)
-13-
Page 17
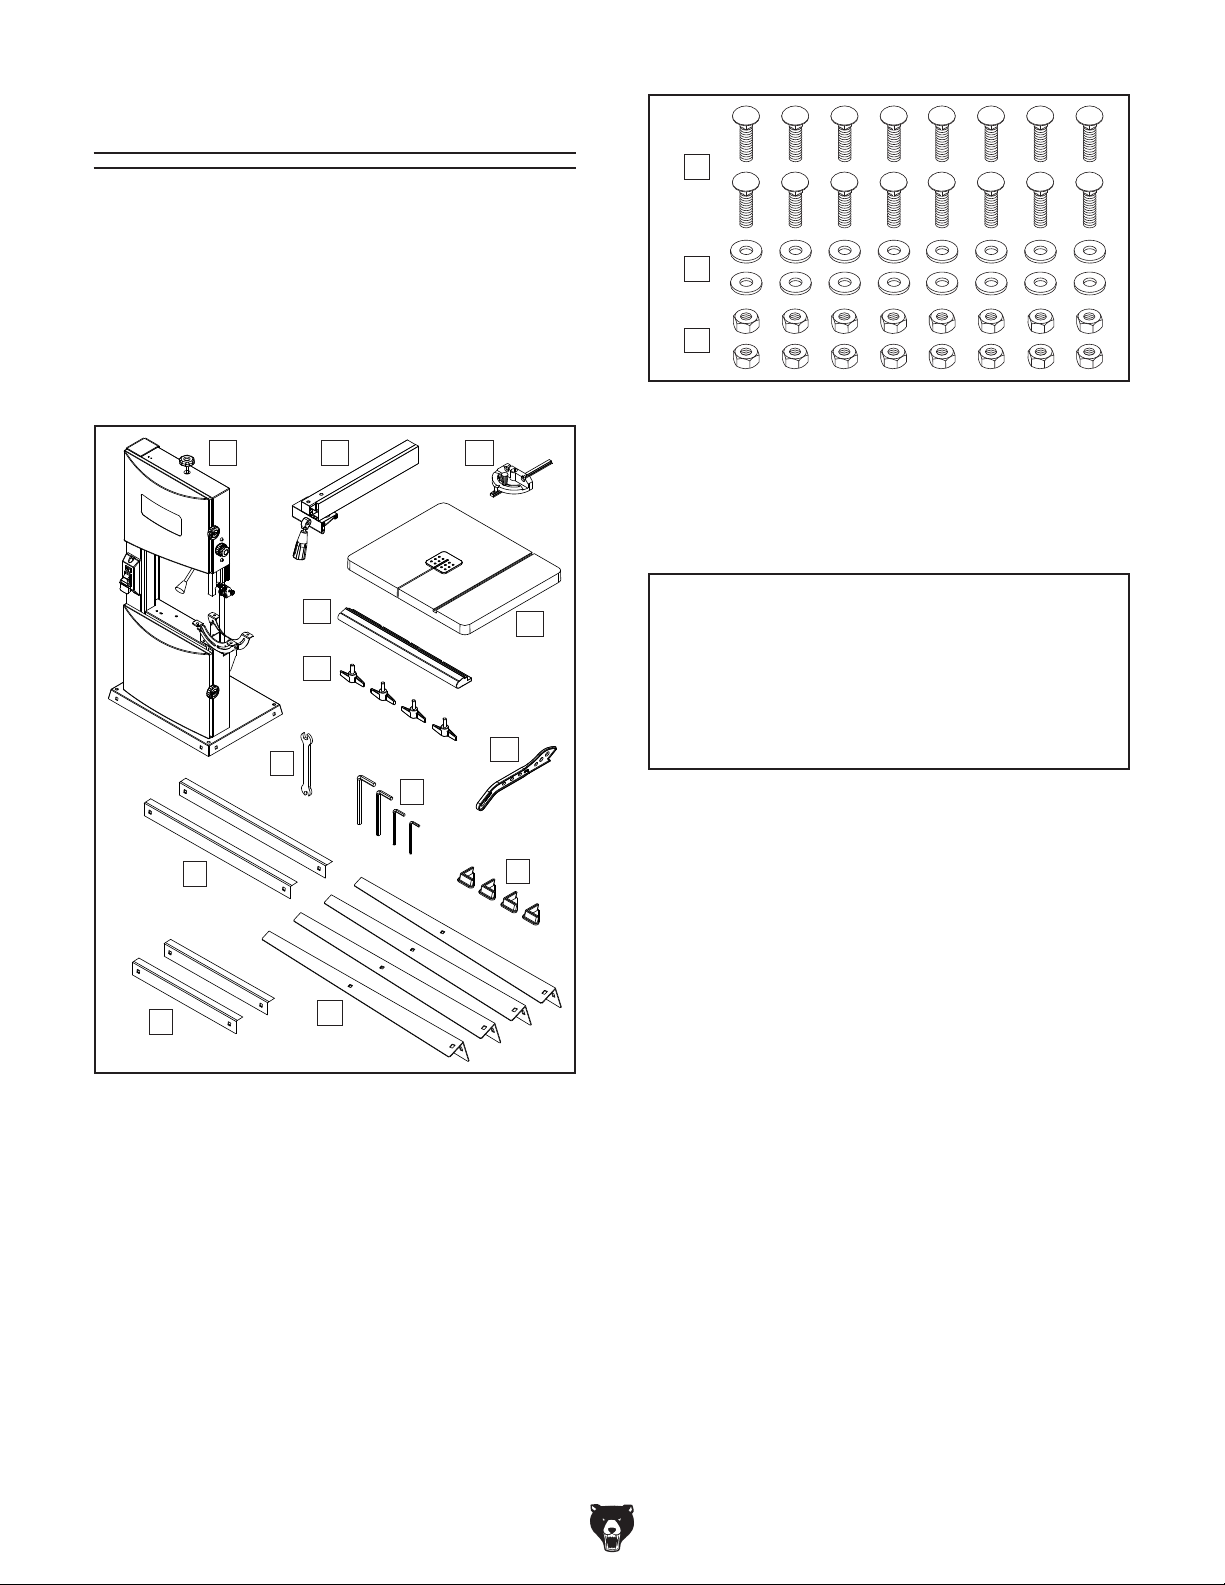
Inventory
The following is a list of items shipped with your
machine. Before beginning setup, lay these items
out and inventory them.
If any non-proprietary parts are missing (e.g. a
nut or a washer), we will gladly replace them; or
for the sake of expediency, replacements can be
obtained at your local hardware store.
N
O
P
Figure 9. Hardware.
A
K
L
B
E
F
H
I
M
C
D
G
J
Hardware (Figure 9) Qty
N. Carriage Bolts M8-1.25 x 16 ..................... 16
Flat Washers 8mm ................................... 16
O.
Hex Nuts M8-1.25 ..................................... 16
P.
NOTICE
If you cannot find an item on this list, carefully check around/inside the machine and
packaging materials. Often, these items get
lost in packaging materials while unpacking or they are pre-installed at the factory.
Figure 8. Inventory.
Inventory (Figure 8) Qty
A. Bandsaw ..................................................... 1
Rip Fence Assembly .................................. 1
B.
Miter Gauge ................................................ 1
C.
Table w/Insert ............................................. 1
D.
Fence Rail .................................................. 1
E.
F. Wing Bolts M8-1.25 x 18 ............................ 4
Push Stick .................................................. 1
G.
Open-End Wrench 10 x 13mm ................... 1
H.
Hex Wrenches 3, 4, 5, 6mm .................1 Ea.
I.
Rubber Feet ............................................... 4
J.
Stand Braces (Long) .................................. 2
K.
Stand Braces (Short) .................................. 2
L.
Stand Legs ................................................. 4
M.
-14-
Model G0948 (Mfd. Since 08/21)
Page 18
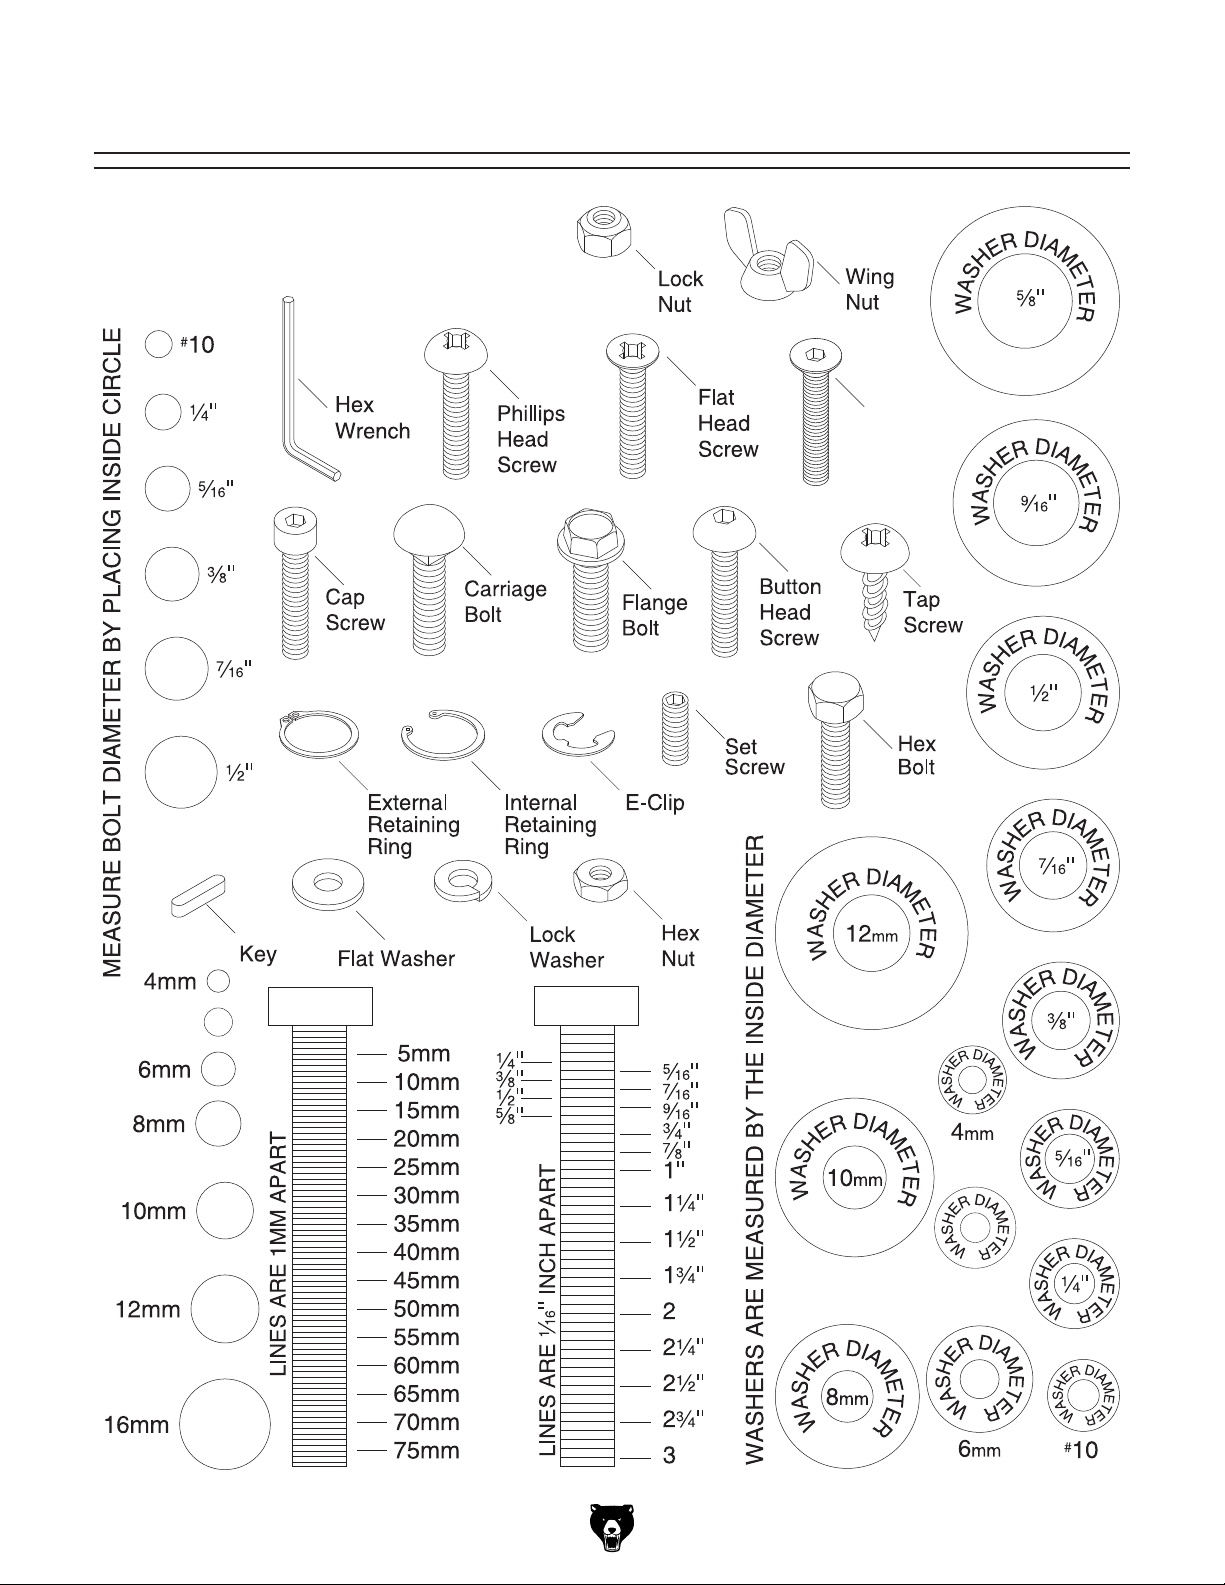
Hardware Recognition Chart
USE THIS CHART TO MATCH UP
HARDWARE DURING THE INVENTORY
AND ASSEMBLY PROCESS.
Flat
Head
Cap
Screw
5mm
Model G0948 (Mfd. Since 08/21)
5mm
-15-
Page 19
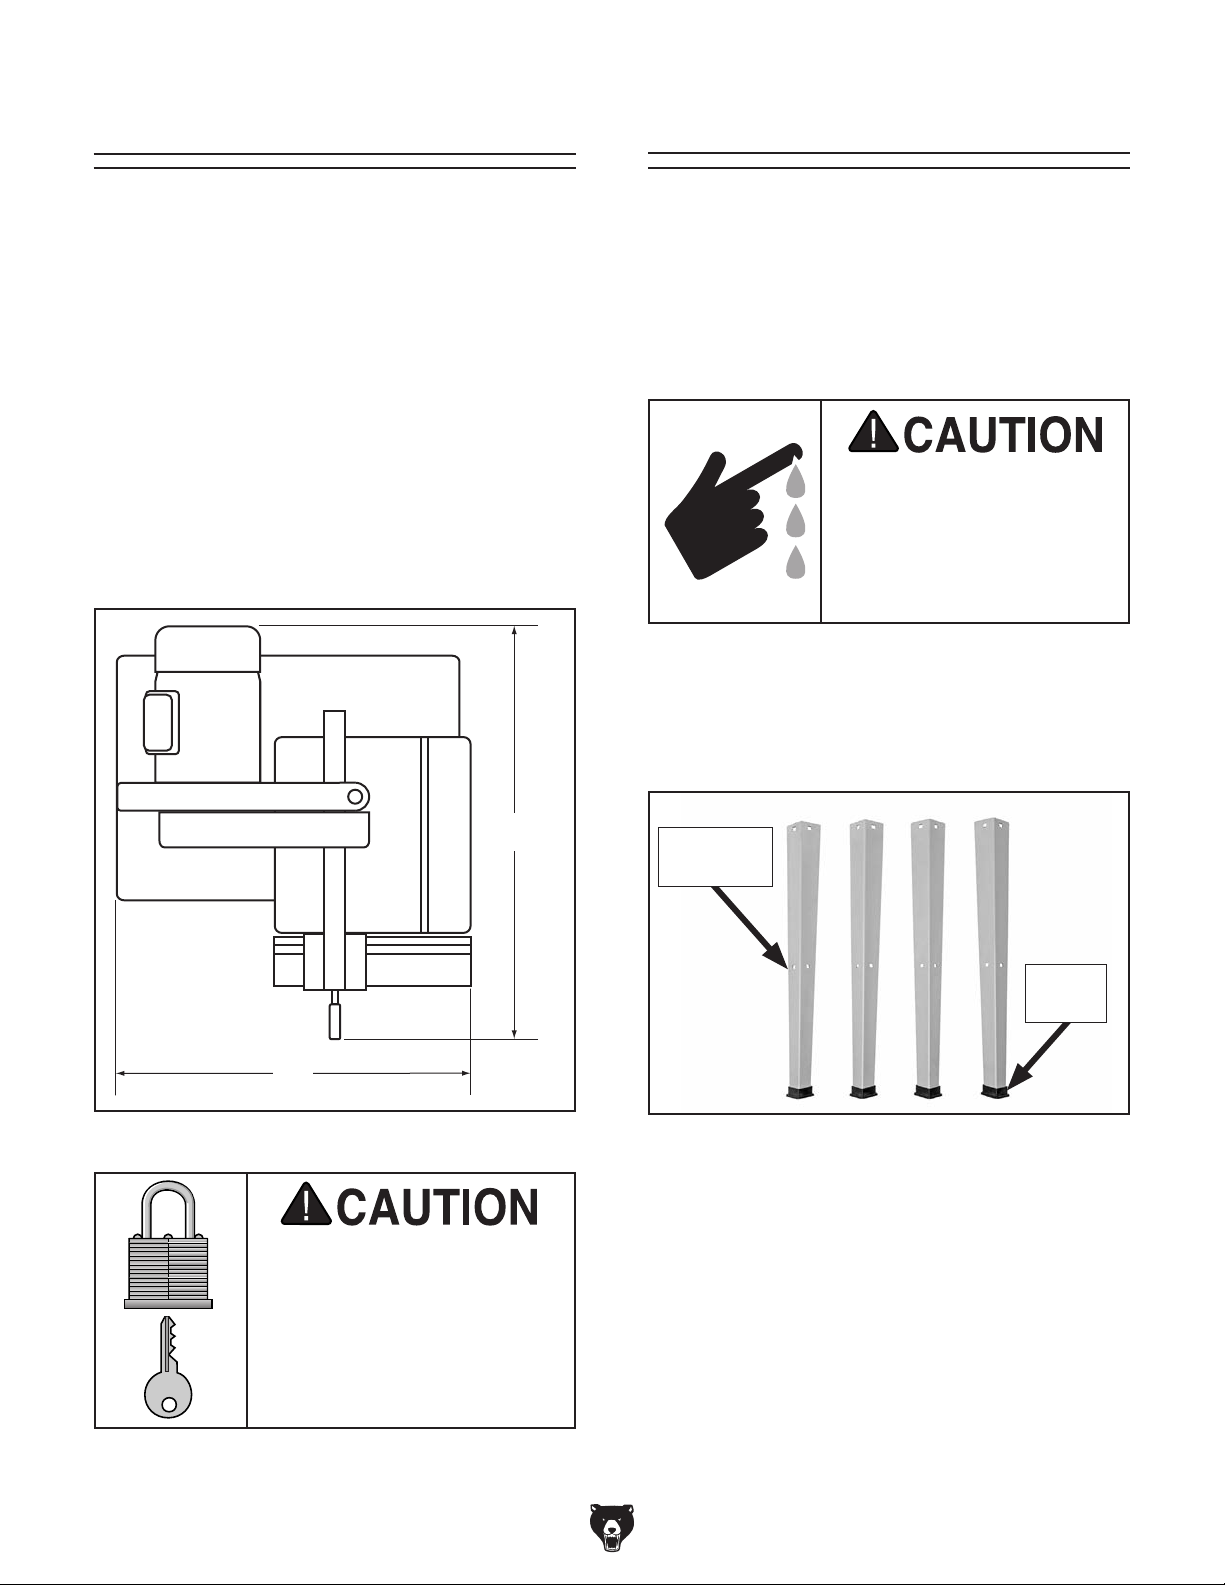
Site Considerations
Refer to the Machine Data Sheet for the weight
and footprint specifications of your machine.
Some workbenches may require additional reinforcement to support the weight of the machine
and workpiece materials.
vised around this machine.
or disable start switch or
Consider anticipated workpiece sizes and additional space needed for auxiliary stands, work
tables, or other machinery when establishing a
location for this machine in the shop. Below is
the minimum amount of space needed for the
The machine must be fully assembled before it
can be operated. Before beginning the assembly
process, refer to
and gather
all
goes smoothly, first clean any
covered or coated in heavy-duty rust preventative (if
applicable).
Workbench Load
Placement Location
Assembly
Needed for Setup
listed items. To ensure the assembly process
parts that are
LACERATION HAZARD!
Bandsaw blades and some
sheet metal parts are
sharp. Wear heavy leather
gloves while handling to
reduce risk of being cut.
To assemble machine:
211/2"
28"
Figure 10. Minimum working clearances.
Children and visitors may be
seriously injured if unsuper-
Locate (4) stand legs (see Figure 11) and
1.
attach (1) rubber foot to bottom of each leg.
Stand Leg
(1 of 4)
Foot
(1 of 4)
Figure 11. Rubber feet attached to stand legs.
Lock entrances to the shop
power connection to prevent
-16 -
unsupervised use.
Model G0948 (Mfd. Since 08/21)
Page 20
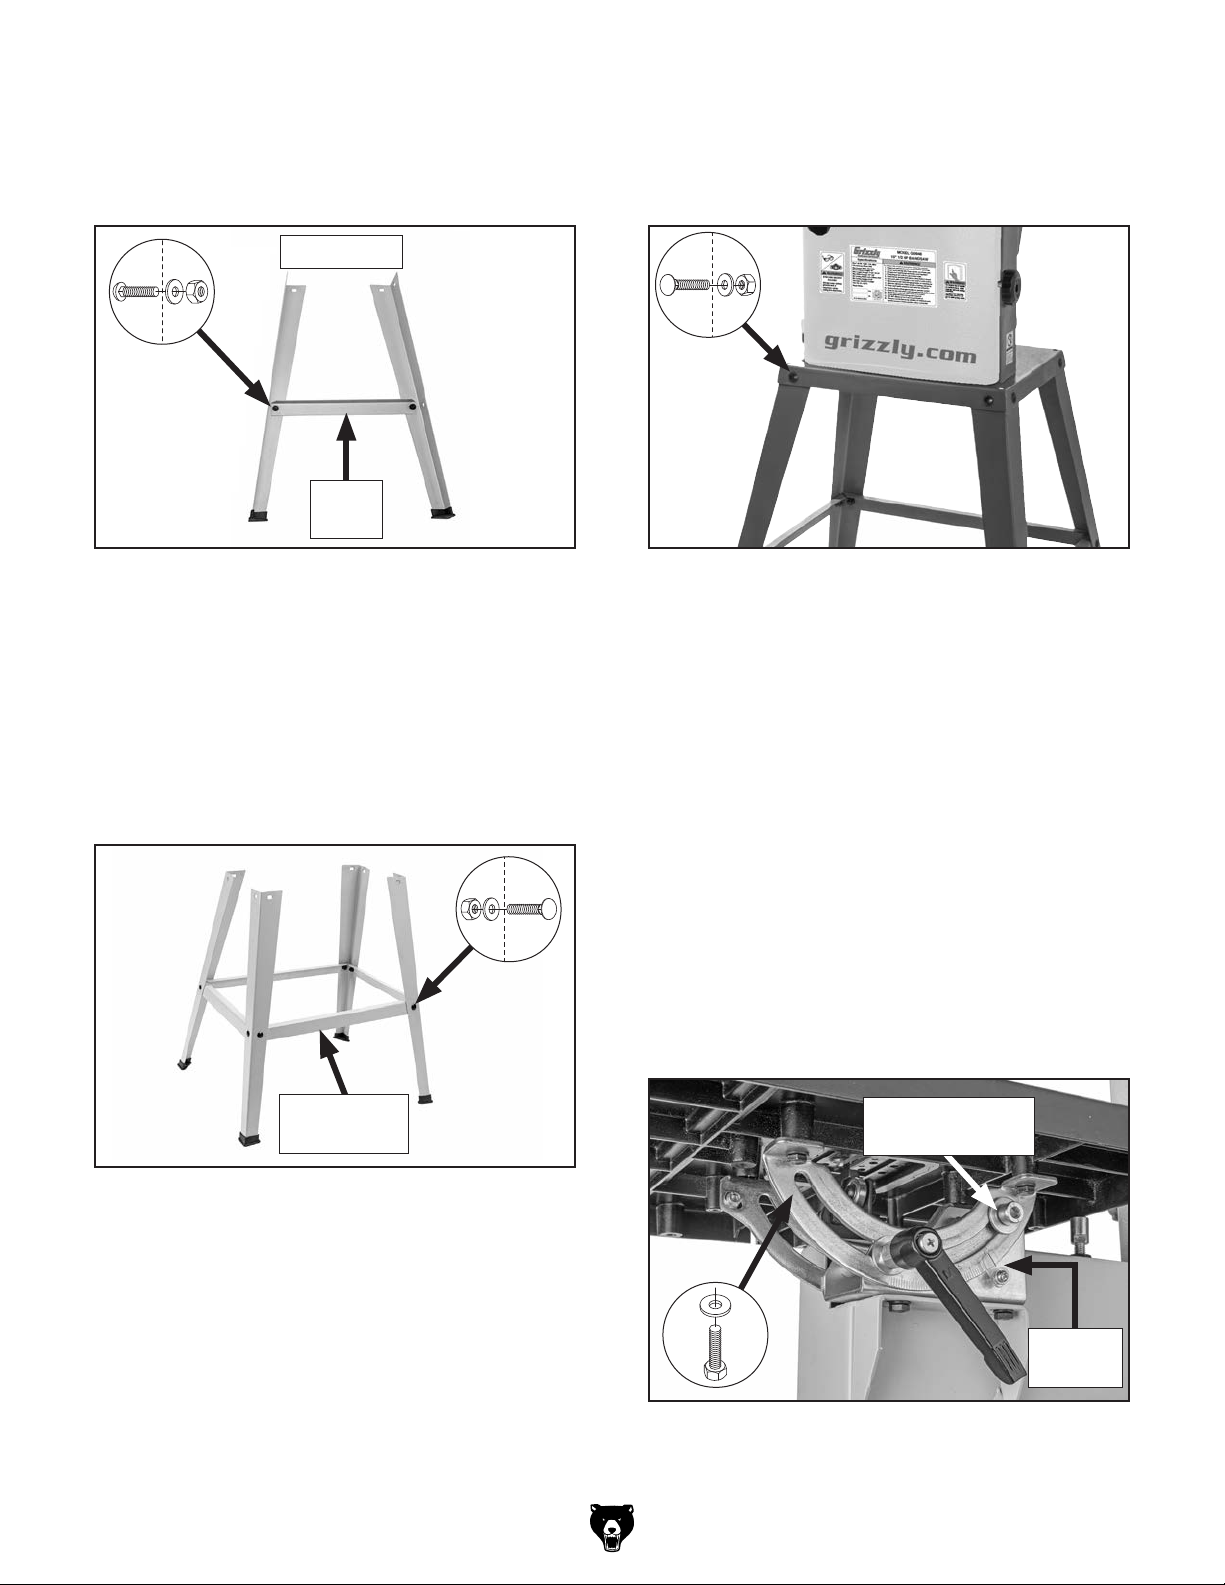
2. Attach (1) short brace to (2) stand legs with
(2) M8-1.25 x 16 carriage bolts, 8mm flat
washers, and M8-1.25 hex nuts, as shown in
Figure 12. Only finger tighten for now.
Stand Legs
Have an assistant position machine base
5.
over top of stand (see Figure 14), and secure
with (8) M8-1.25 x 16 carriage bolts, 8mm flat
washers, and M8-1.25 hex nuts.
x 2
Short
Brace
Figure 12. Stand legs attached to short braces.
Repeat Step 2 with remaining (1) short brace
3.
and (2) stand legs.
Attach (2) leg assemblies together with (2)
4.
long braces using (4) M8-1.25 x 16 carriage
bolts, 8mm flat washers, and M8-1.25 hex
nuts, as shown in Figure 13. Only finger
tighten for now.
x 4
x 8
Figure 14. Machine attached to stand.
Ensure machine is level, side to side and front
6.
to back, then tighten all fasteners installed in
Steps 2–5.
Remove (4) pre-installed M6-1 x 10 hex bolts
7.
and 6mm flat washers from base of table, and
loosen (2) shoulder screws (see Figure 15)
securing trunnions to trunnion bracket.
Note: For operations requiring a high degree
of accuracy, tighten shoulder screws securing trunnions to trunnion bracket to increase
table rigidity.
Page reference 16
Long Brace
(1 of 2)
Figure 13. Leg assemblies attached with long
braces.
Model G0948 (Mfd. Since 08/21)
Slide table past saw blade through table slot,
8.
and secure table to trunnions with fasteners
removed in Step 7 (see Figure 15).
Shoulder Screw
(1 of 2)
x 4
Figure 15. Table attached to trunnions.
Scale
Indicator
-17-
Page 21
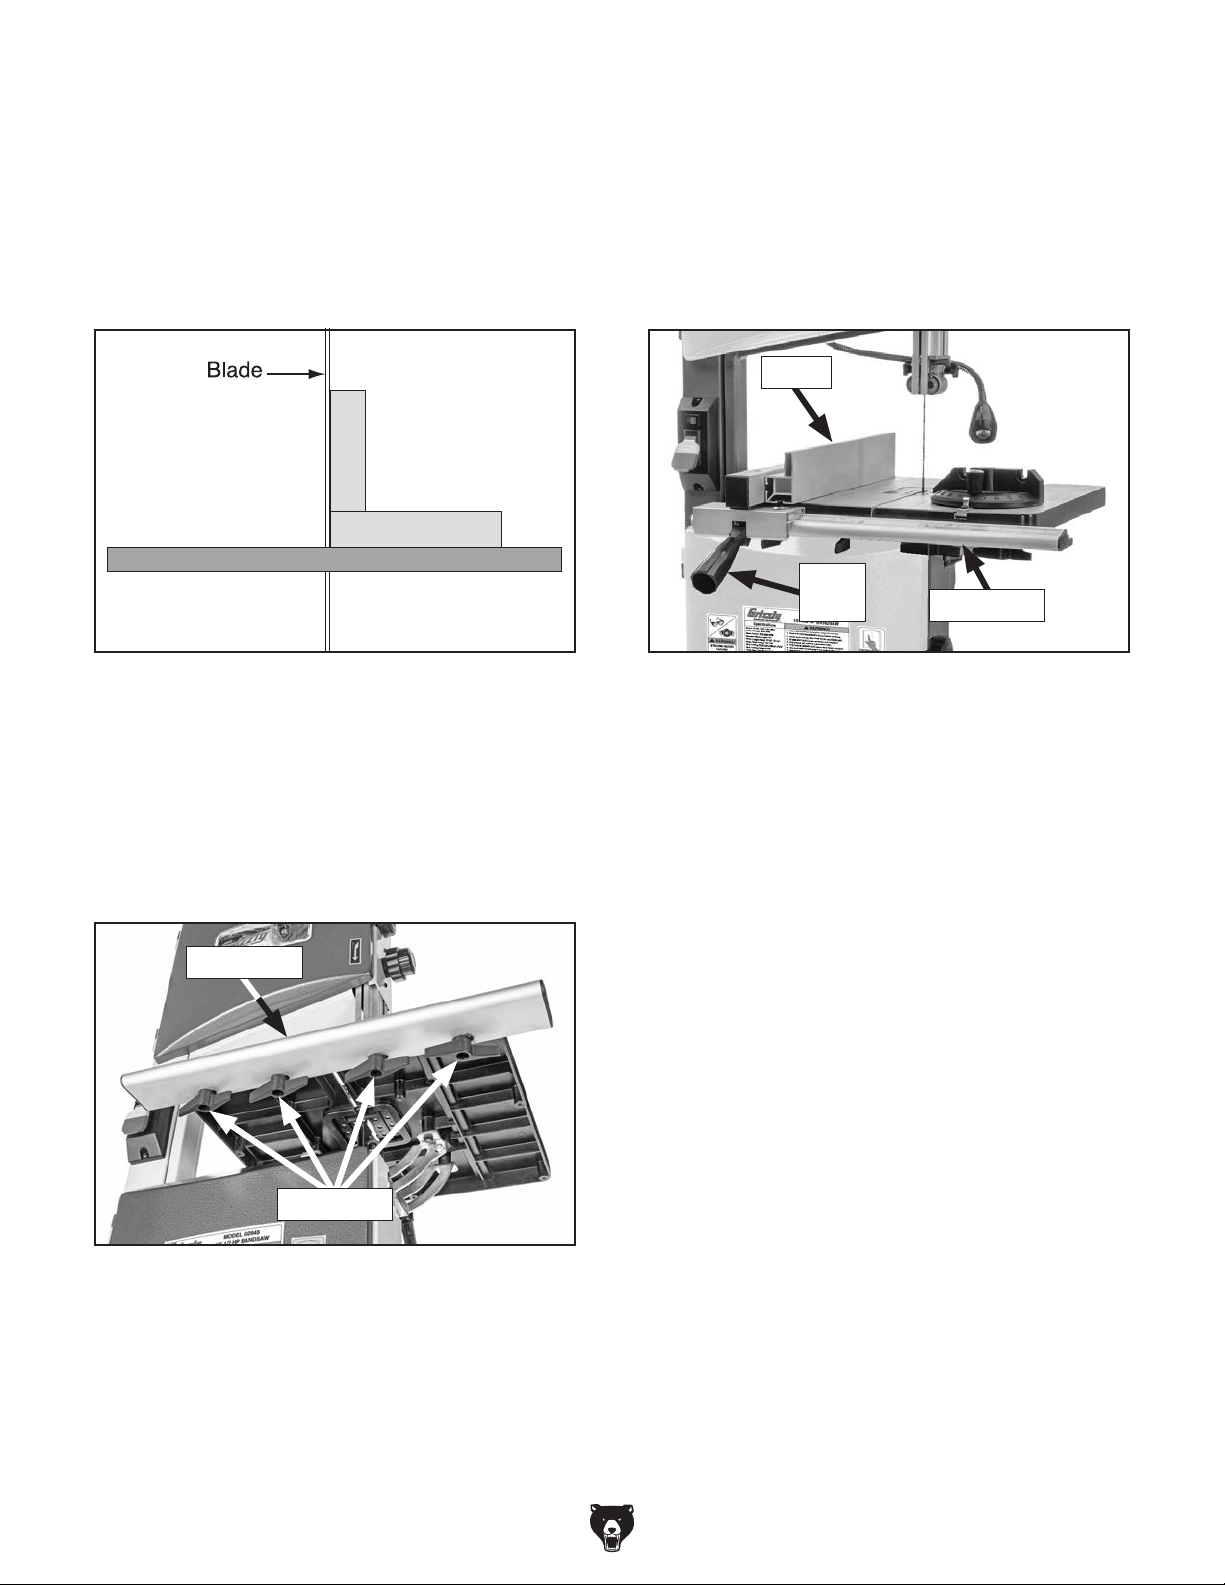
9. Completely raise upper blade guide assem-
bly, then place machinist's square flat on
table, against side of blade (see Figure 16).
Loosen table lock lever, and tilt table until
10.
square is flat against side of blade, as illustrated in Figure 16. When complete, tighten
lock lever.
Square
Table
13. Install fence on fence rail, as shown in
Figure 18.
Note: Fence lock lever (see Figure 18)
needs to be in up position when fitting fence
onto fence rail. Once fence snaps onto fence
rail, push lock lever down to secure fence in
position.
Fence
Lock
Lever
Fence Rail
Figure 16. Using a square to adjust table
perpendicular to the side of blade.
11.
Loosen screw on scale indicator (see Figure
15 on Page 17), set indicator to "0", and
tighten screw.
Attach fence rail to front of table with (4)
12.
M8-1.25 x 18 wing bolts (see Figure 17).
Fence Rail
Wing Bolts
Figure 18. Fence installed on fence rail.
Figure 17. Fence rail attached to front of table.
-18-
Model G0948 (Mfd. Since 08/21)
Page 22
Dust Collection
Adjustment
Overview
This machine creates a lot of wood chips/
dust during operation. Breathing airborne
dust on a regular basis can result in permanent respiratory illness. Reduce your risk
by wearing a respirator and capturing the
dust with a dust-collection system.
2" Dust Port.......................................... 10 0 CF M
3" Dust Port.......................................... 250 CFM
4" Dust Port.......................................... 400 CFM
Do not confuse this CFM recommendation with
the rating of the dust collector. To determine the
CFM at the dust port, you must consider these
variables: (1) CFM rating of the dust collector,
(2) hose type and length between the dust collector and the machine, (3) number of branches
or wyes, and (4) amount of other open lines
throughout the system. Explaining how to calculate these variables is beyond the scope of
this manual. Consult an expert or purchase a
good dust collection "how-to" book.
The bandsaw is one of the most versatile woodworking machines. However, it has multiple components that must be properly adjusted for the
best cutting results.
For practical and safety reasons, some adjustments and test operations must be performed
before performing other necessary adjustments.
Below is an overview of all the adjustments and
the order in which they should be performed:
Initial Blade Tracking
1.
Test Run
2.
Tensioning Blade
3.
Adjusting Blade Support Bearings
4.
Adjusting Blade Guide Bearings
5.
Aligning Table
6.
Aligning Fence
7.
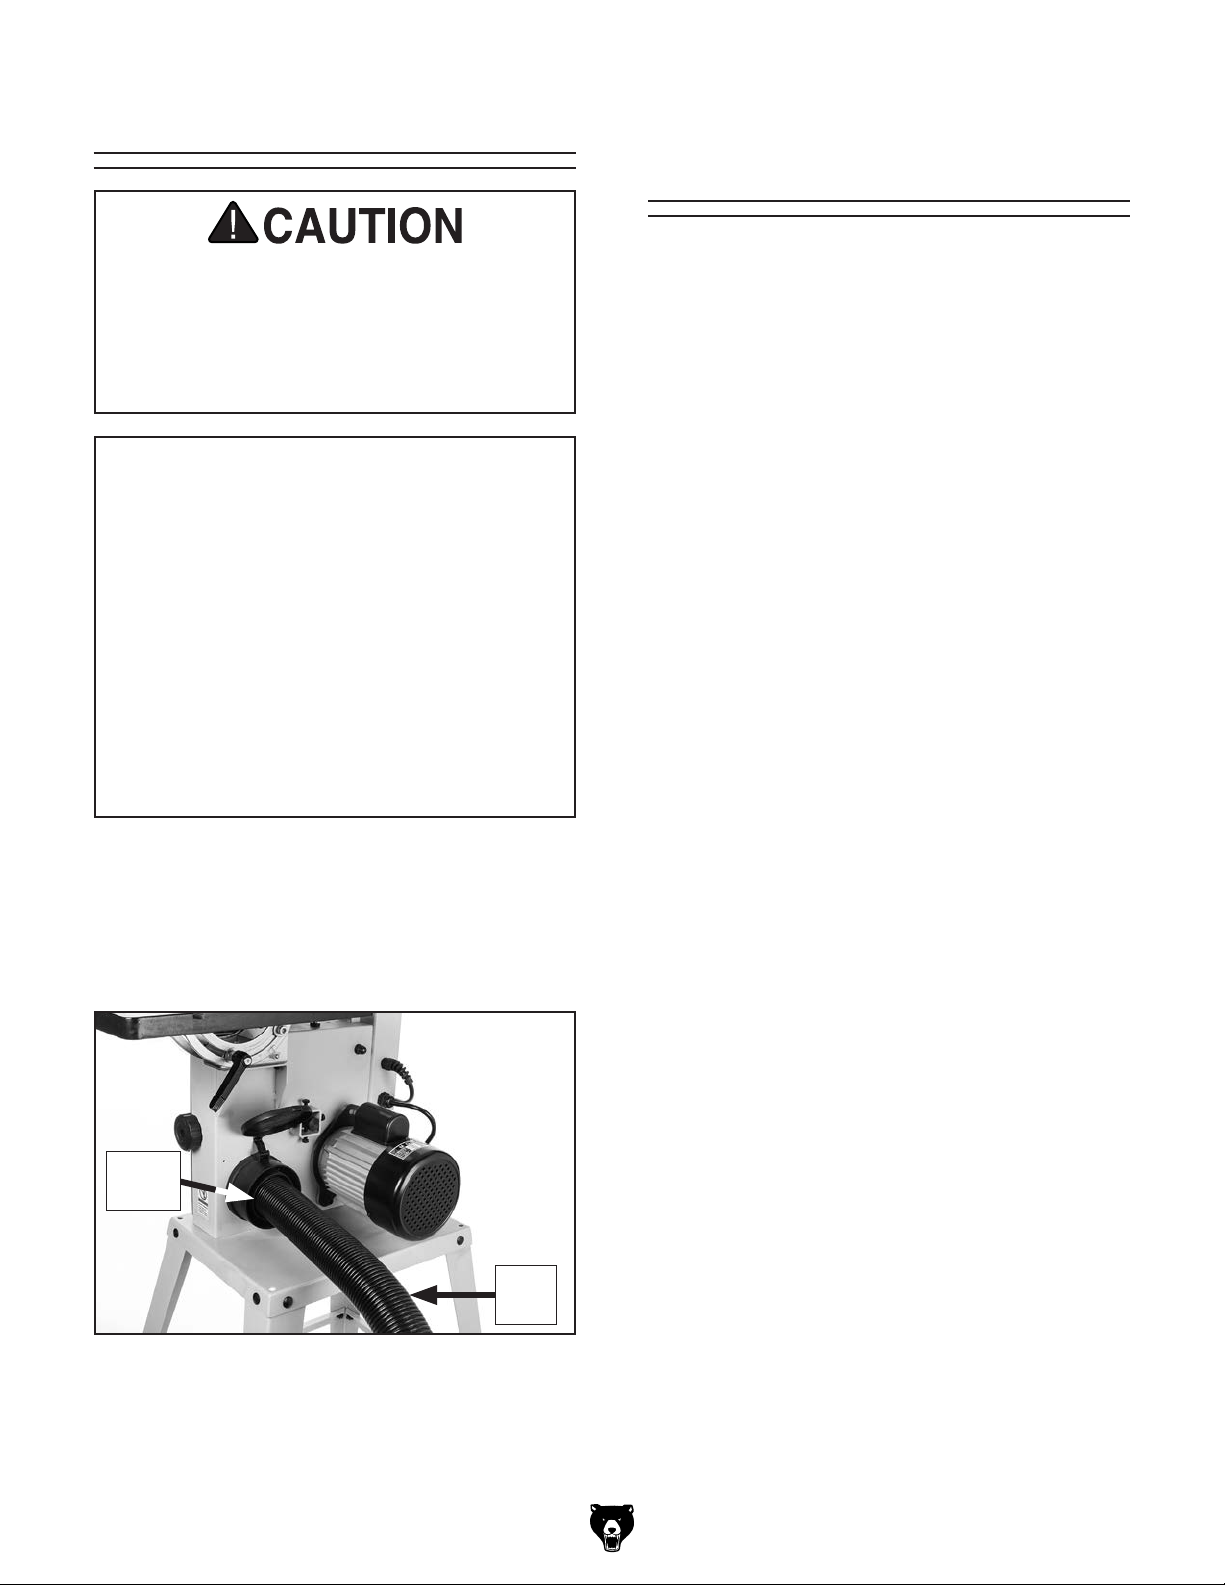
To connect a dust collection hose:
1. Fit 2", 3" or 4" dust hose over dust port, as
shown in Figure 19, and secure it in place
with a hose clamp.
Hose
Clamp
Dust
Hose
Figure 19. Example of 2" dust hose attached to
dust port.
2. Gently pull hose to make sure it does not
come off. A tight fit is necessary for proper
performance.
Model G0948 (Mfd. Since 08/21)
-19 -
Page 23
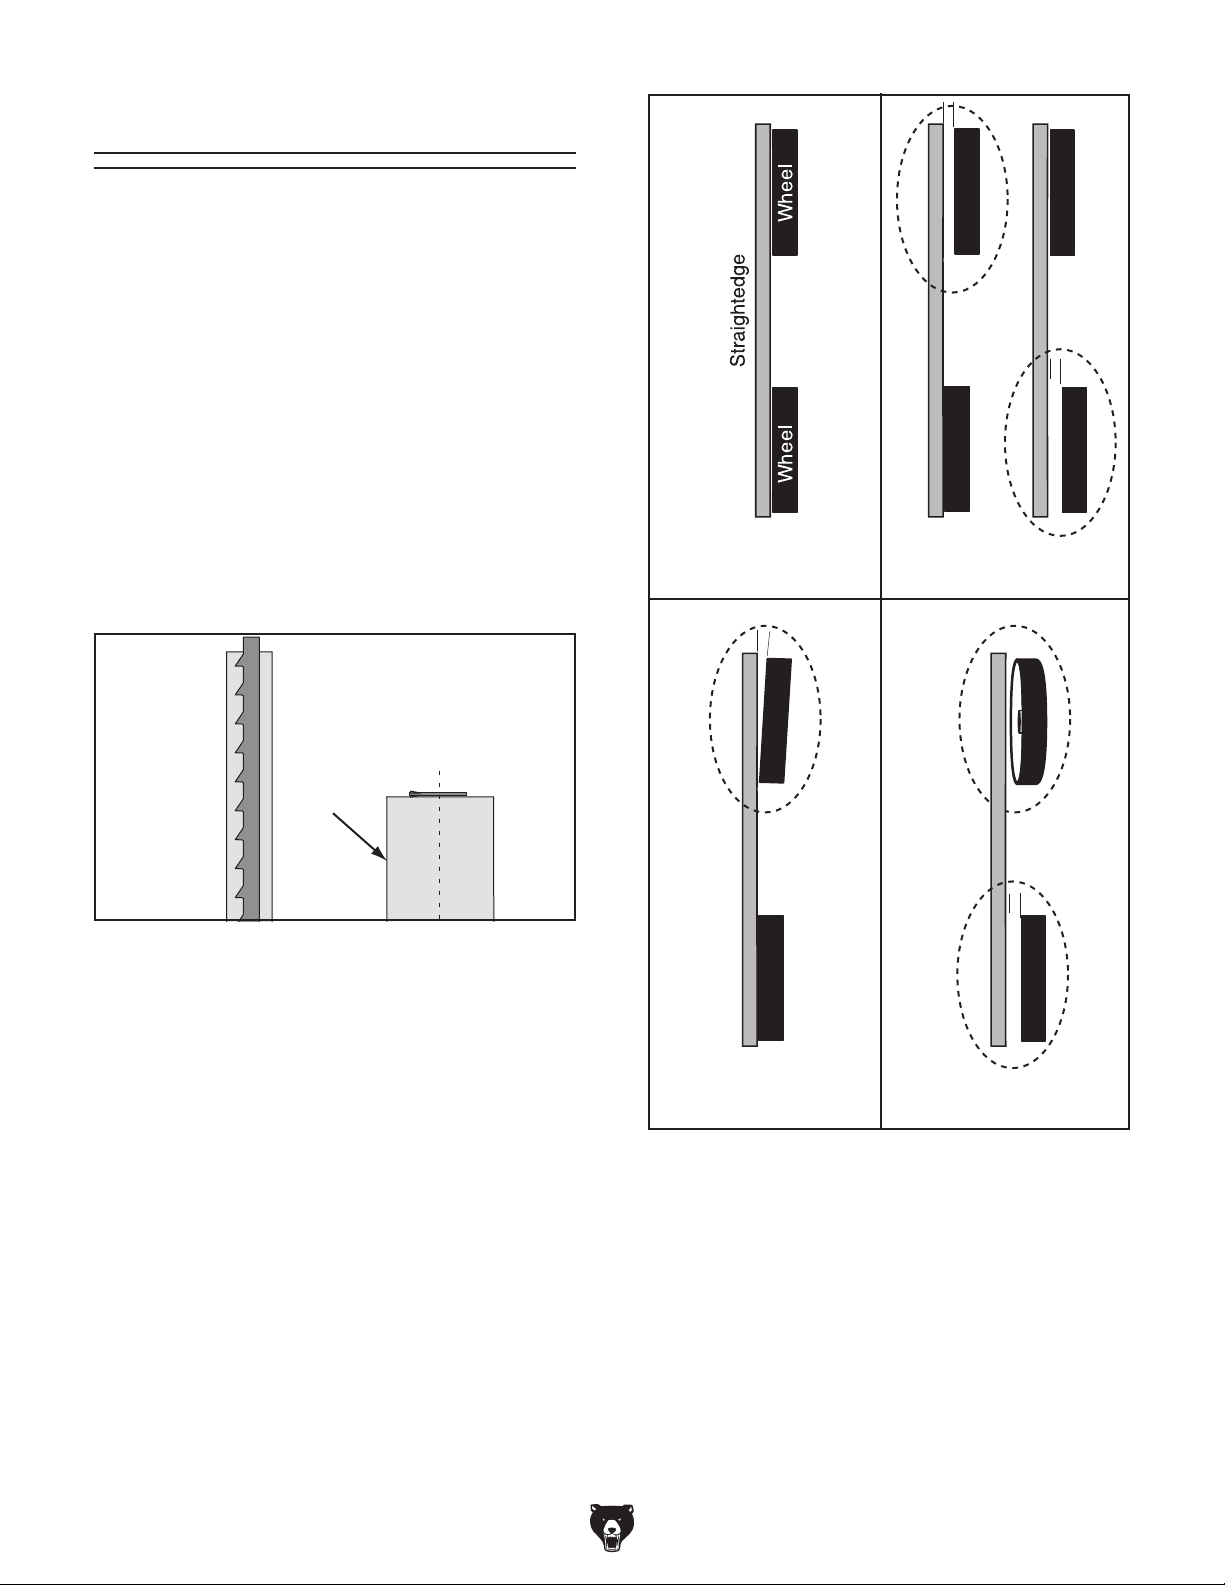
Initial Blade Tracking
"Tracking" refers to how the blade rides on the
bandsaw wheels. Proper tracking is important
for maintaining bandsaw adjustments, achieving correct blade tension, and cutting accurately. Improper tracking reduces cutting accuracy,
causes excess vibrations, and places stress on
the blade and other bandsaw components. The
shape of the wheels and the orientation of the
wheels in relation to each other determine how
the blade tracks.
Bandsaw wheels are either flat or crowned and
both shapes track differently. The G0948 has
crowned wheels. As the wheels spin, a properly
tracking blade naturally tracks at the center of the
wheel (see
Figure 20).
PROPER TRACKING
Parallel And
Coplanar
or
Parallel But Not
Coplanar
Blade Centered
on Wheel
Blade
Centered
on Wheel
Figure 20. Blade centered on crown of wheel.
The bandsaw wheels must be aligned for optimal
machine performance. Properly aligned wheels
are parallel and coplanar (see
Improper blade tension and cutting practices can
negatively affect blade tracking. Familiarizing
yourself with the ideas and conditions described
Figure 21 will help you recognize when your
in
wheel alignment may need to be adjusted (refer to
Aligning Wheels on Page 53 for detailed instructions on adjusting the tracking).
Wheel
Figure 21).
Coplanar But
Not Parallel
Figure 21. Wheel alignment and misalignment
examples.
The wheels on the G0948 were aligned at the factory, so center tracking is the only adjustment that
needs to be performed when the saw is new. This
adjustment is necessary before turning the saw
on or performing other adjustments.
Not Coplanar or
Parallel
-20-
Model G0948 (Mfd. Since 08/21)
Page 24
Once assembly is complete, test run the machine
to ensure it is properly connected to power and
safety components are functioning correctly.
If you find an unusual problem during the test run,
immediately stop the machine, disconnect it from
power, and fix the problem BEFORE operating the
machine again. The
table in the
SERVICE section of this manual can help.
Serious injury or death can result from
Tool(s) Needed Qty
Protective Gloves..........................................1 Pr.
Hex Wrenches 4, 5mm
To adjust blade tracking:
DISCONNECT MACHINE FROM POWER!
1.
Adjust upper and lower blade guides away
2.
from blade, and raise upper guides all the way
up (refer to Adjusting Blade Guide Bearings
on Page
Note: When adjusting the blade tracking for
the test run in this procedure, the blade must
have approximately the same amount of tension as when under operating conditions.
After the test run is successfully completed,
you will be instructed on how to more accurately tension the blade for optimum results.
Rotate tension adjustment knob clockwise to
3.
apply tension to blade (see Figure
25 for detailed instructions).
................................1 Ea.
22).
6.
Rotate upper wheel by hand several times
and watch how blade rides on wheel (see
Figure
this concept).
— If the blade rides in the center of the upper
— If the blade does not ride in the center of
Spin upper wheel with one hand and slowly
7.
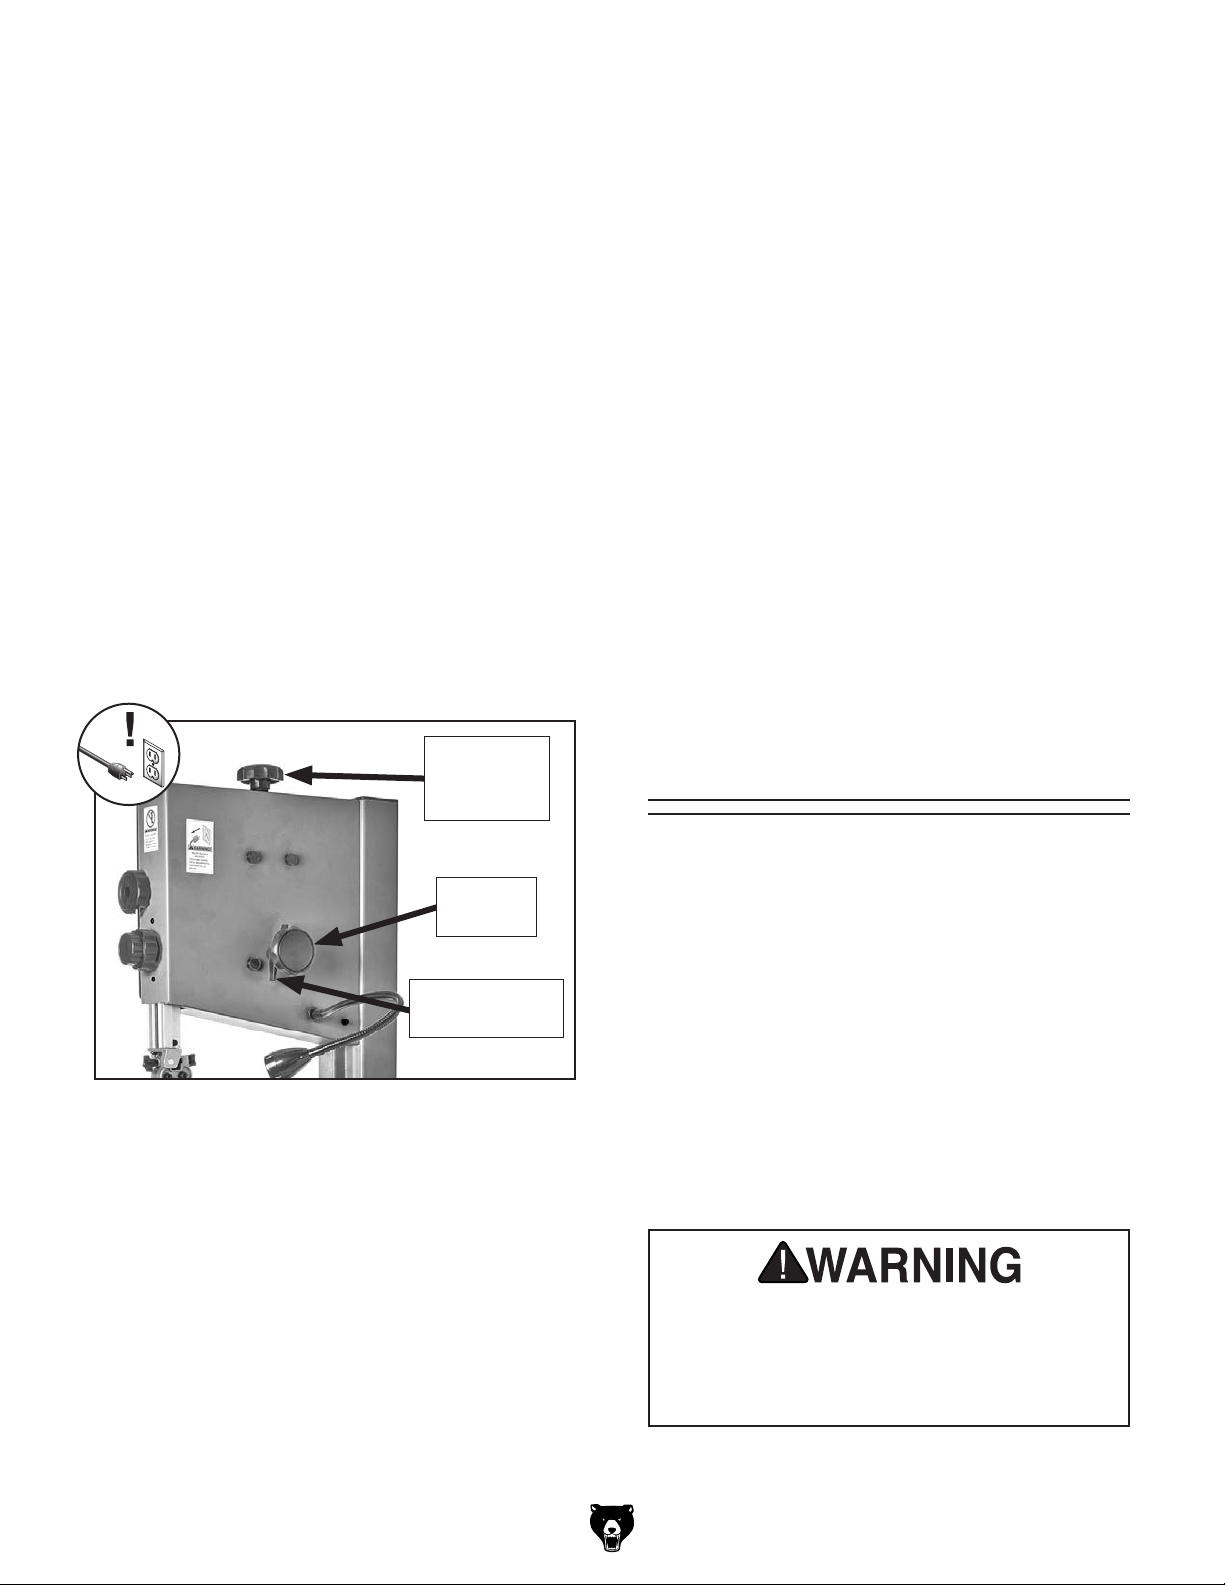
adjust tracking knob (see Figure 22) with
other hand until blade consistently tracks in
center of wheel.
Turn tracking knob lock lever clockwise to
8.
secure setting.
Close and secure upper wheel cover before
9.
operating bandsaw.
20 on Page 20 for an illustration of
wheel, it is properly tracking and you are
done with this procedure.
the upper wheel, it is not properly tracking;
continue with the next step to adjust it.
Tension
Adjustment
Knob
Tracking
Knob
Tracking Knob
Lock Lever
Figure 22. Blade tension and tracking controls.
4. Open upper wheel cover.
Push blade toward fence with moderate
5.
pressure to check if there is approximately
1
⁄4" deflection. If not, rotate tension adjustment knob as needed until blade is properly
tensioned.
Test Run
Troubleshooting
The test run consists of verifying the following:
1) The motor powers up and runs correctly,
and 2) the removable key on the switch works
correctly.
using this machine BEFORE understanding
its controls and related safety information.
DO NOT operate, or allow others to operate,
machine until the information is understood.
Model G0948 (Mfd. Since 08/21)
-21-
Page 25
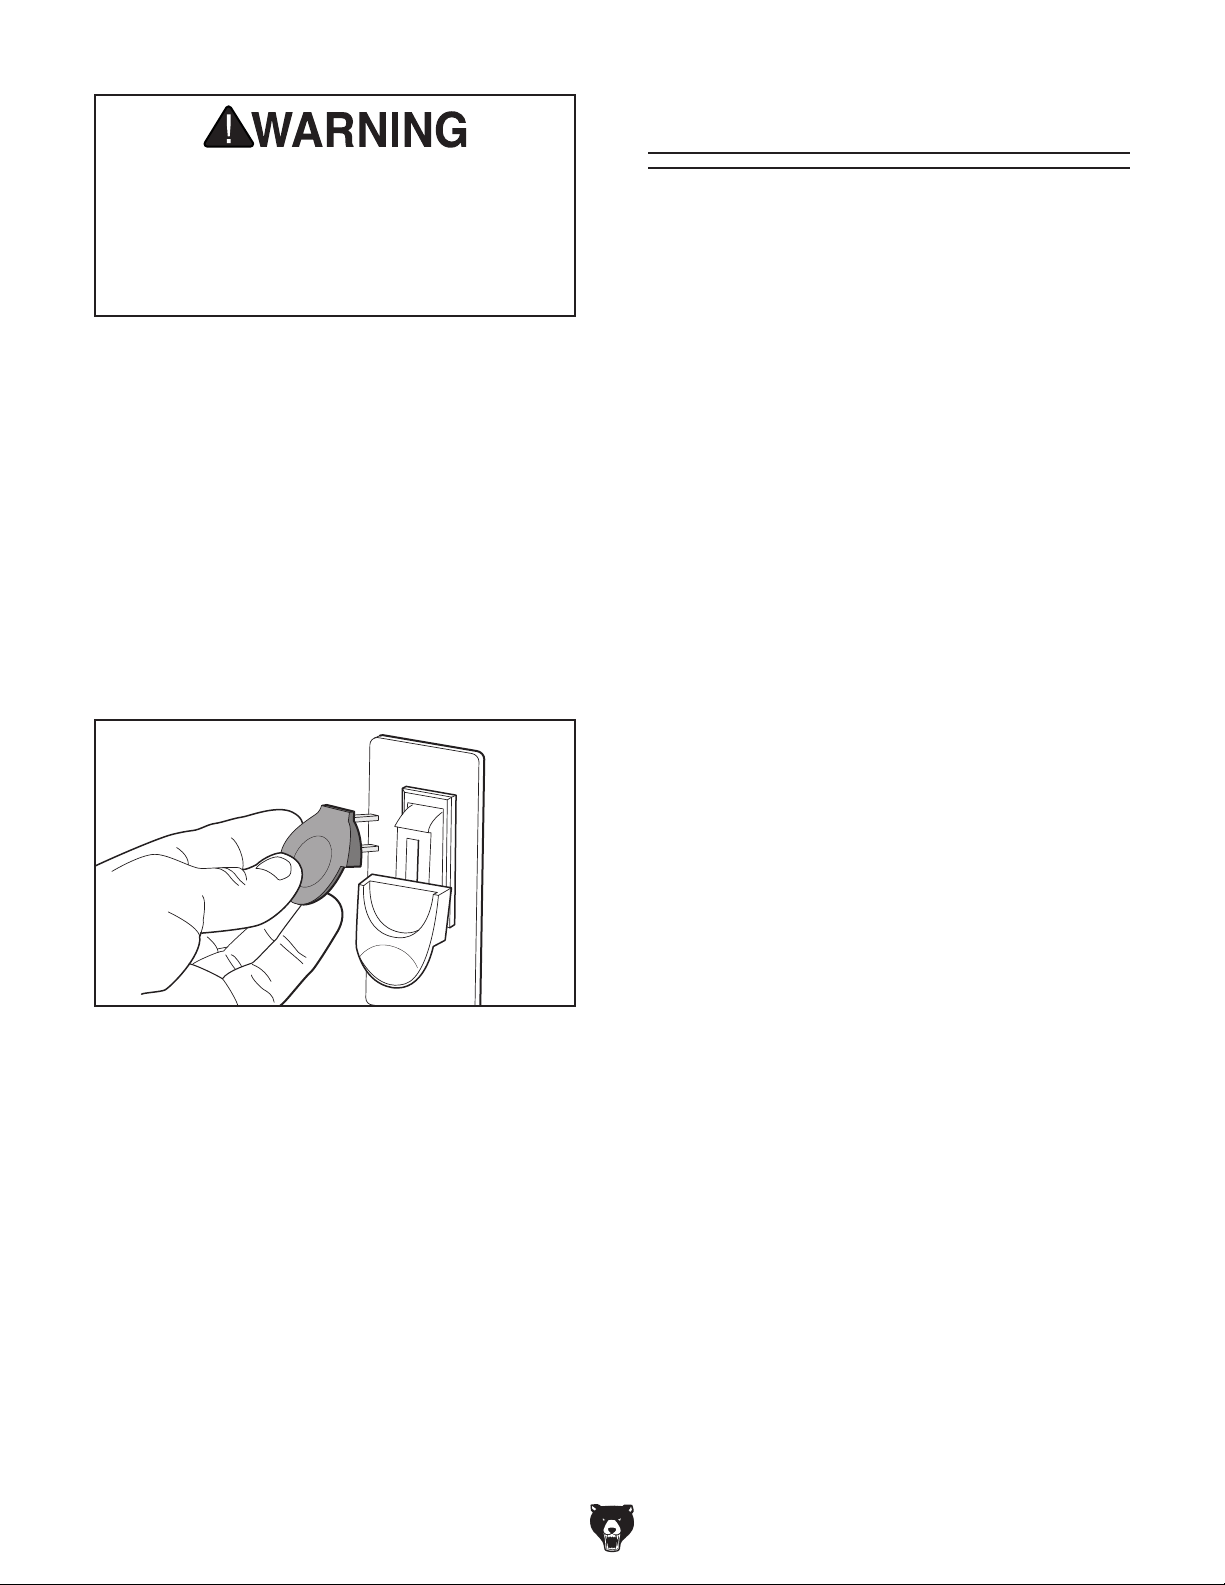
DO NOT start machine until all preceding
setup instructions have been performed.
Operating an improperly set up machine
may result in malfunction or unexpected results that can lead to serious injury,
death, or machine/property damage.
To test run machine:
Tensioning Blade
A properly tensioned blade is essential for making accurate cuts, maximizing the blade life, and
making other bandsaw adjustments. However, a
properly tensioned blade will not compensate for
cutting problems caused by excessive feed rate,
hardness variations between workpieces, and
improper blade selection.
1. Clear all setup tools away from machine.
2. Connect machine to power supply.
3. Turn machine ON, verify motor operation,
then turn machine OFF.
The motor should run smoothly and without
problems or unusual noises.
4.
Remove key, as shown in Figure 23.
Optimal cutting results for any type of workpiece
are achieved through a combination of correct
blade selection, proper blade tension, properly
adjusted blade guides and other bandsaw components, and using an appropriate feed rate.
Improper blade tension is unsafe, produces inaccurate and inconsistent results, and introduces
unnecessary wear on bandsaw components.
Over-tensioning the blade increases the chance
of the blade breaking or wheel misalignment.
Under-tensioned blades wander excessively
while cutting and will not track properly during
operation.
The method used to tension the blade is often
a matter of preference. This manual describes
two methods: the flutter method and the deflection method. Either method will help you properly
tension the blade. Experience and personal preference will help you decide which method you
prefer.
Figure 23. Removing key from ON/OFF paddle
switch.
5. Try to start machine with ON/OFF paddle
switch. The machine should not start.
— If the machine does not start, the switch is
working as designed.
— If the machine does start, immediately
stop the machine. The switch is not working correctly. This safety feature must work
properly before proceeding with regular
operations. Call Tech Support for help.
-22-
Note: Tensioning the blade before the Test Run
was an approximate tension. The following procedures fine-tune the blade tension.
Model G0948 (Mfd. Since 08/21)
Page 26
The Flutter Method
Using the flutter method, you intentionally loosen
the blade until it just passes the point of being
too loose (when it begins to flutter). Then you
gradually tighten the blade until proper tension is
reached.
To tension bandsaw blade using flutter
method.
1. DISCONNECT MACHINE FROM POWER!
Make sure blade is properly tracking as
2.
instructed in Initial Blade Tracking on
Page 20.
Raise guide post all the way, and move upper
3.
and lower guide bearings away from blade.
Rotate blade tension adjustment knob clock-
4.
wise to apply tension to blade.
Connect bandsaw to power, then turn it ON.
5.
Using blade tension adjustment knob, slowly
6.
decrease blade tension until you see the
blade start to flutter.
. Slowly increase tension until blade stops flut-
7
tering, then tighten blade tension adjustment
knob an additional
8. DISCONNECT MACHINE FROM POWER!
1
⁄8 to 1⁄4 of a turn.
The Deflection Method
The deflection method is much more subjective
than the flutter method. Each blade will deflect
differently and every user will determine what
"moderate pressure" means. The following are
general guidelines for tensioning the blade with
this method.
To tension bandsaw blade using deflection
method:
1. DISCONNECT MACHINE FROM POWER!
Make sure blade is properly tracking as
2.
instructed in Initial Blade Tracking on
Page 20.
Raise guide post all the way and move upper
3.
and lower guide bearings away from blade.
Rotate blade tension adjustment knob clock-
4.
wise to apply tension to blade.
5. Using moderate pressure, push center of the
blade sideways with one finger.
— If the blade deflects approximately 1⁄4", it is
properly tensioned. Proceed to
— If the blade deflects less than 1⁄4", it is over-
tensioned. Turn the blade tension adjustment knob counterclockwise two full turns
and repeat
Step 5.
Step 6.
9. Adjust blade guides as described in Adjusting
Blade Support Bearings and Adjusting
Blade Guide Bearings on Pages 24–25.
Model G0948 (Mfd. Since 08/21)
— If the blade deflects 1⁄4" or more, the blade
is not properly tensioned. Apply tension to
the blade incrementally and repeat
until properly tensioned.
6. Adjust blade guides as described in Adjusting
Blade Support Bearings and Adjusting
Blade Guide Bearings on
Pages 24–25.
Step 5
-23-
Page 27
Adjusting Blade
Support Bearings
The support bearings are positioned behind the
blade near the blade guides and prevent the blade
from pushing backward during cutting operations.
Proper adjustment of the support bearings helps
you make accurate cuts and prevents the blade
teeth from coming in contact with the blade guides
while cutting. If this happens the blade "tooth
set" can be ruined, which will greatly reduce the
blade's ability to make good cuts.
0.016''
Figure 25. Bearing positioned 0.016" away from
back of blade.
IMPORTANT: To ensure best results while cutting, make sure blade is tracking (see Initial
Blade Tracking on Page 20) and tensioned (see
Blade Tensioning on Page 22) correctly before
performing this procedure.
Adjusting Upper Support Bearing
Tool(s) Needed Qty
Feeler Gauge 0.016" .......................................... 1
To adjust upper support bearing:
. DISCONNECT MACHINE FROM POWER!
1
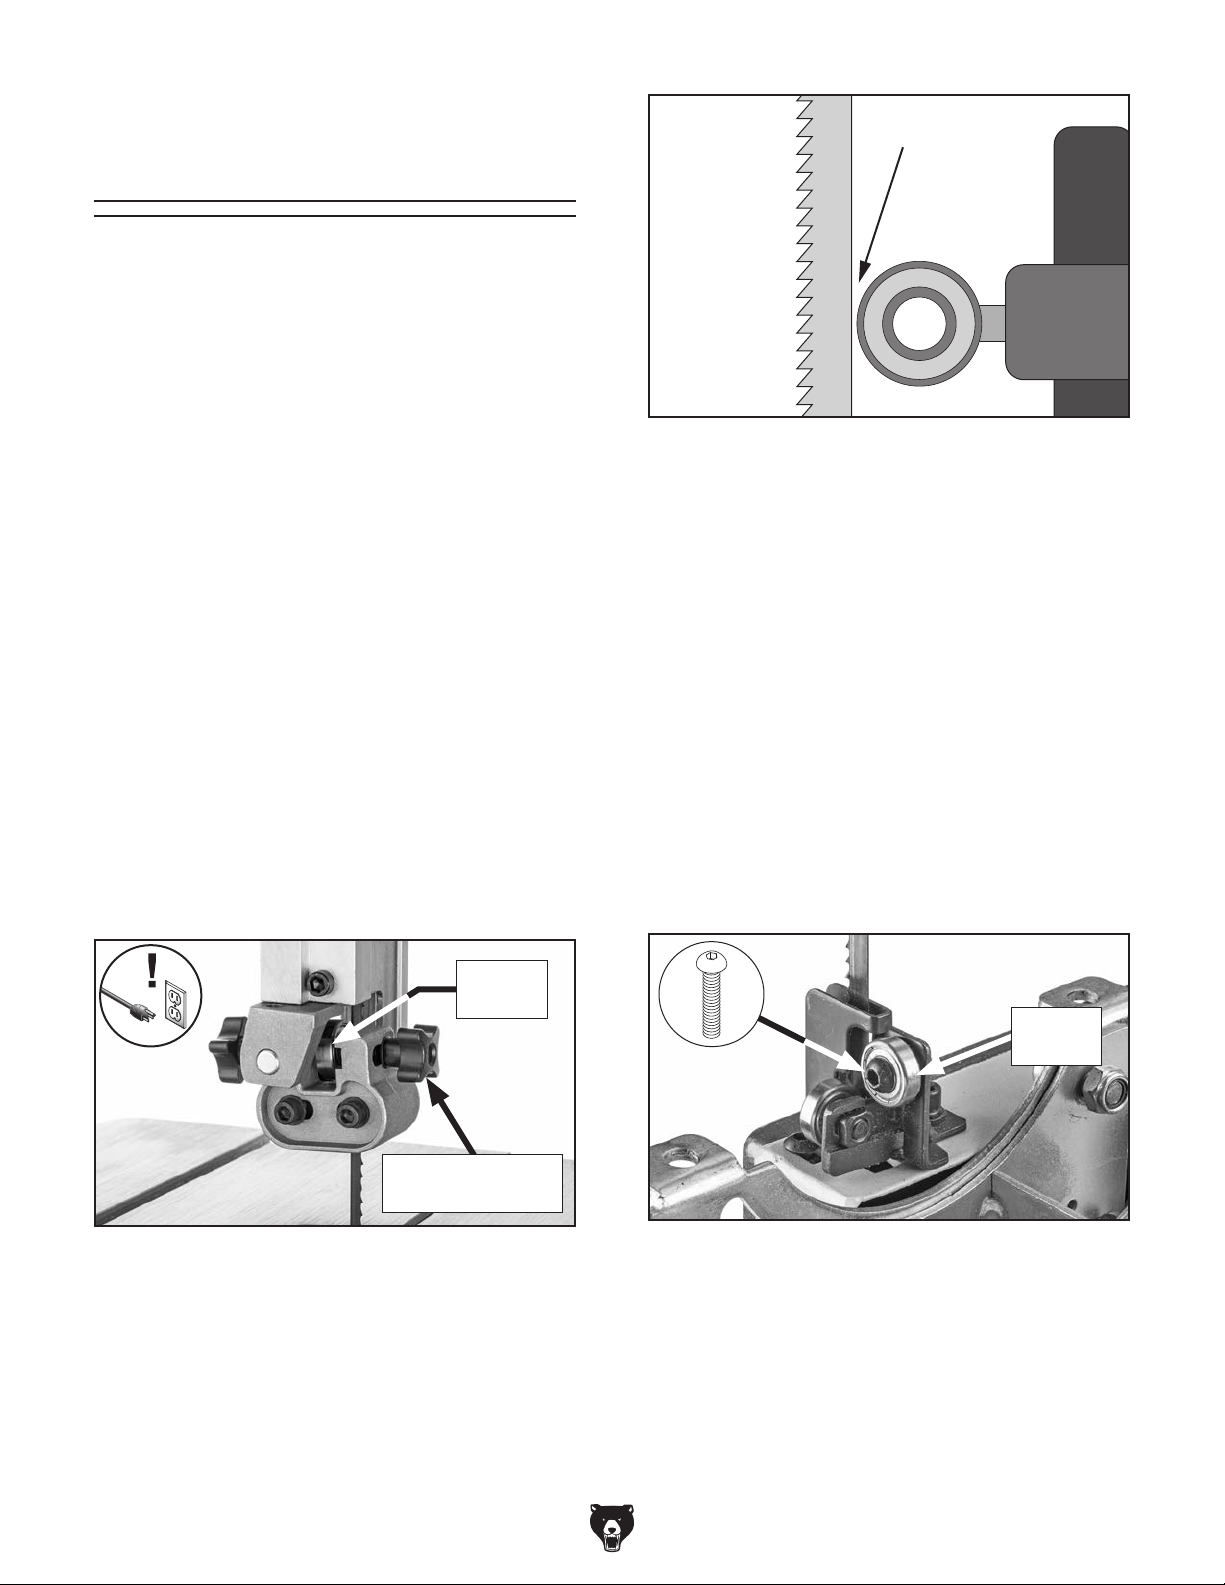
Loosen support bearing adjustment knob
2.
(see Figure 24).
Support
Bearing
4.
Tighten adjustment knob to lock support
bearing in place.
Adjusting Lower Support Bearing
Tool(s) Needed Qty
Wrench or Socket 10mm ................................... 1
Hex Wrench 4mm
Feeler Gauge 0.016"
To adjust lower support bearing:
1. DISCONNECT MACHINE FROM POWER!
Loosen button head cap screw (see
2.
Figure 26).
.............................................. 1
.......................................... 1
Support
Bearing
Support Bearing
Adjustment Knob
Figure 24. Upper support bearing components.
Position support bearing approximately 0.016"
3.
away from back of blade (see Figure 25).
Note: The main purpose of this adjustment
is to prevent the blade from being pushed
backward far enough that the blade guides
will contact (and ruin) the "tooth set" of the
blade during cutting operations.
-24-
Figure 26. Location of lower support bearing
(table removed for clarity).
3. Position support bearing approximately 0.016"
away from the back of the blade, as illustrated
Figure 25. This can be measured with a
in
feeler gauge.
Tighten button head cap screw loosened in
4.
Step 2.
Model G0948 (Mfd. Since 08/21)
Page 28
Adjusting Blade
Guide Bearings
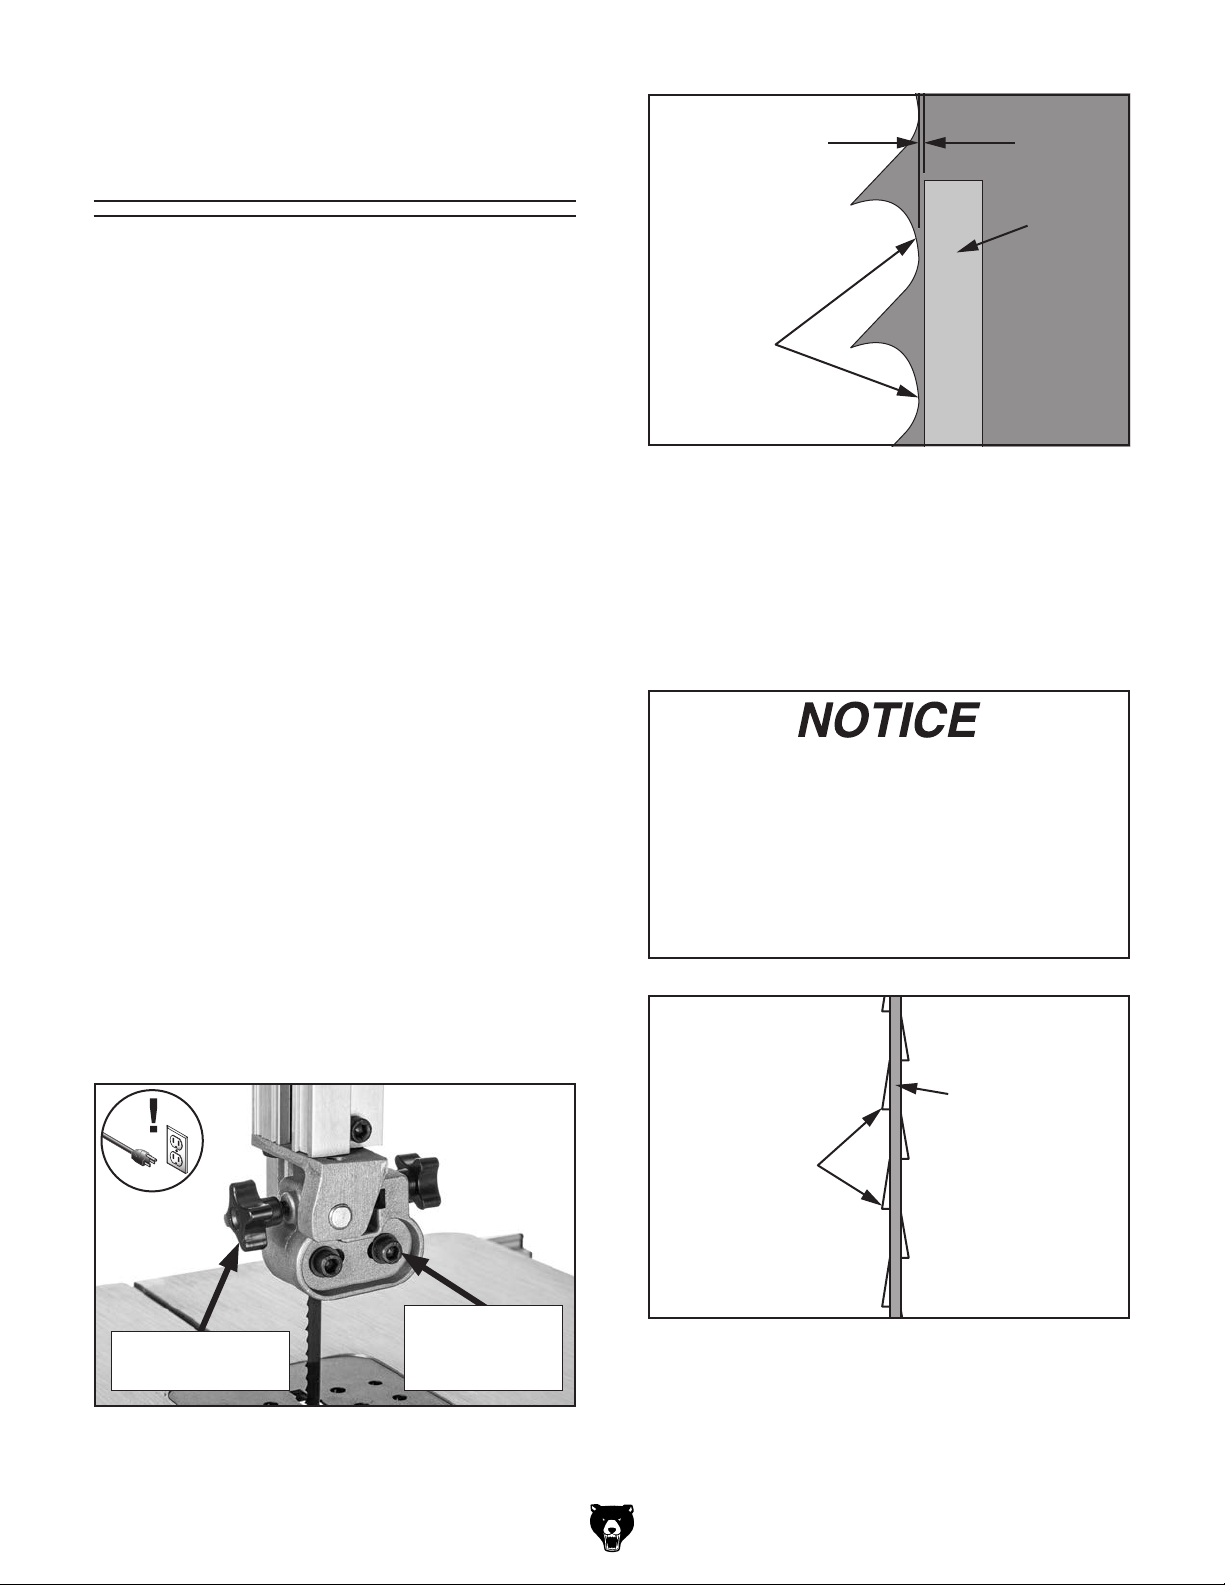
The blade guide bearings can be adjusted leftto-right, as well as front-to-back, relative to the
blade. Properly adjusted blade guide bearings
provide side-to-side support, from just behind the
gullets to the back of the blade, to help keep the
blade straight while cutting.
IMPORTANT: Make sure the blade is tracking
(refer to Initial Blade Tracking on Page 20) and
tensioned (see Tensioning Blade on Page
correctly before performing this procedure.
Adjusting Upper Blade Guide Bearings
Tool(s) Needed Qty
Hex Wrench 4mm .............................................. 1
Feeler Gauge 0.016"
To adjust upper blade guide bearings:
.......................................... 1
22)
Approximately
0.016"
Blade
Guide
Bearing
(1 of 2)
Blade
Gullets
Figure 28. Blade guide bearing positioned just
behind blade gullets.
Note: With wider blades, it may not be possi-
ble to bring the guide bearings just behind the
blade gullets. Position them as far forward as
possible without allowing the guide bearing
housing to touch the back of the blade.
DISCONNECT MACHINE FROM POWER!
1.
Loosen guide block adjustment knob shown
2.
in Figur
bearings just behind blade gullets, as illustrated in Figur
secure setting.
Note: The guide bearings should be posi-
tioned behind the gullets a distance equal to
that of the support bearing behind the blade
(see
Guide Block
Adjustment Knob
e 27, then laterally position guide
e 28, then tighten knob to
Page 24 for reference).
Guide Bearing
Cap Screw
(1 of 2)
Blade teeth are angled out slightly, protruding wider than the blade thickness; this is
known as blade "tooth set" (see Figure 29).
If teeth contact guide bearings during operation, damage may occur. Therefore, the
support bearing must be set to prevent
teeth from contacting guide bearings during
operation (refer to Page 24 for details).
BladeThickness
“Tooth Set”
Wider Than
Blade Thickness
Figure 29. Illustration of blade "tooth set".
Figure 27. Upper guide bearing components.
Model G0948 (Mfd. Since 08/21)
-25-
Page 29
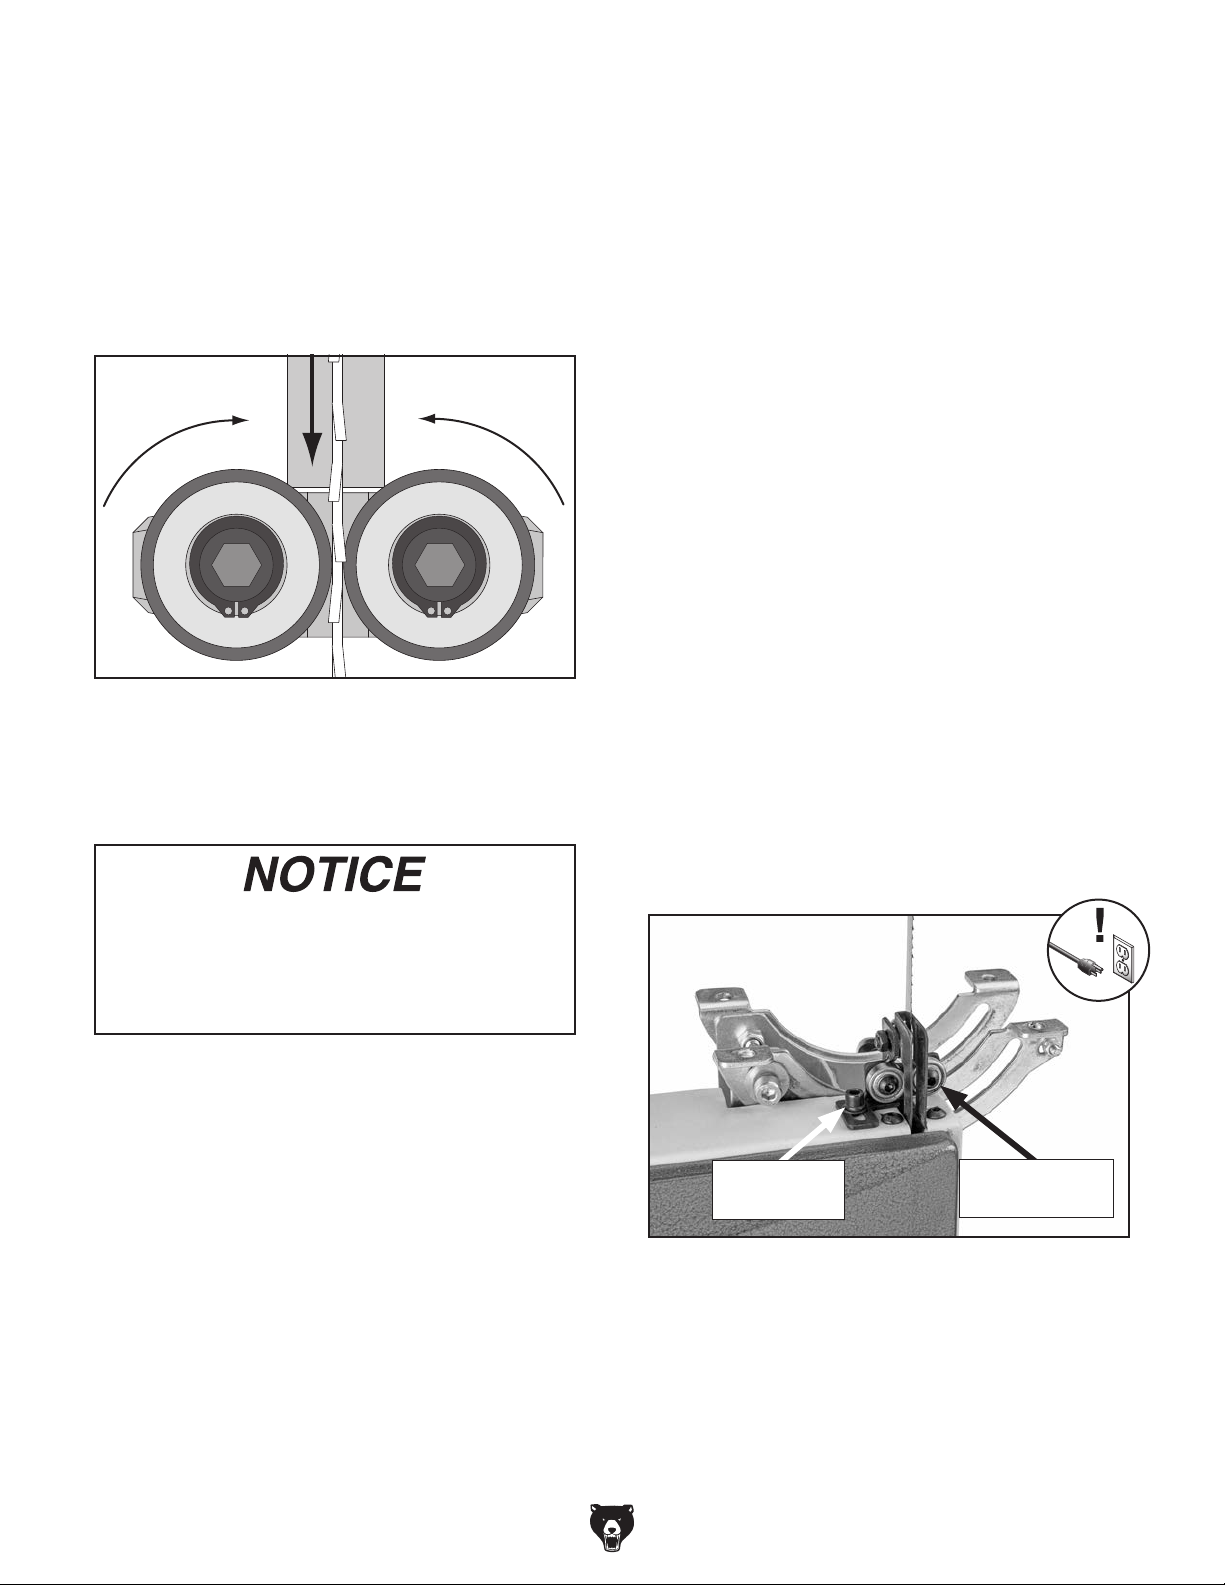
3. Loosen both guide bearing cap screws (see
Figure 27 on Page 25), then position guide
bearings so they evenly and lightly touch
sides of blade (see illustration in
without deflecting it one way or the other.
Figure 30)
Adjusting Lower Blade Guide
Bearings
Tool(s) Needed Qty
Hex Wrenches 4, 5mm ................................1 Ea.
Feeler Gauge 0.016"
.......................................... 1
Note: When the blade guide bearings are
properly adjusted against the blade, they
should lightly rotate as the blade moves.
Figure 30. Blade guide bearings evenly and
lightly touching the sides of the blade.
4.
Tighten cap screws to secure settings.
Re-check setting after tightening.
To adjust lower blade guide bearings:
DISCONNECT MACHINE FROM POWER!
1.
Loosen guide block cap screw (see Figure
2.
31), then laterally position guide bearings
just behind blade gullets, as illustrated in
e 28 on Page 25, then tighten cap
Figur
screw to secure setting.
Note: The guide bearings should be posi-
tioned behind the gullets a distance equal to
that of the support bearing behind the blade
Page 24 for reference).
(see
Loosen both guide bearing screws (see
3.
Figure 31), then position guide bearings so
they evenly and lightly touch sides of blade
(see illustration in
ing it one way or the other.
Note: When the blade guide bearings are
properly adjusted against the blade, they
should lightly rotate as the blade moves.
Figure 30) without deflect-
Whenever changing blade or adjusting
blade tension or tracking, the support and
guide bearings must be re-adjusted before
resuming operation to ensure proper blade
support.
Guide Block
Cap Screw
Figure 31. Lower blade guide components (table
removed for clarity).
4. Tighten screws to secure settings. Re-check
setting after tightening.
Guide Bearing
Screw (1 of 2)
-26-
Model G0948 (Mfd. Since 08/21)
Page 30
Aligning Table
To ensure cutting accuracy, the table should be
aligned so that the miter slot is parallel to the
bandsaw blade.
Item(s) Needed Qty
Precision Straightedge ...................................... 1
Precision Ruler
Square
Hex Wrench 6mm
Wrench or Socket 10mm
Shims
............................................................... 1
................................................. As Needed
Adjusting Miter Slot Parallelism
1. Make sure blade is tracking properly and cor-
rectly tensioned (refer to Pages 20 and 22).
DISCONNECT MACHINE FROM POWER!
2.
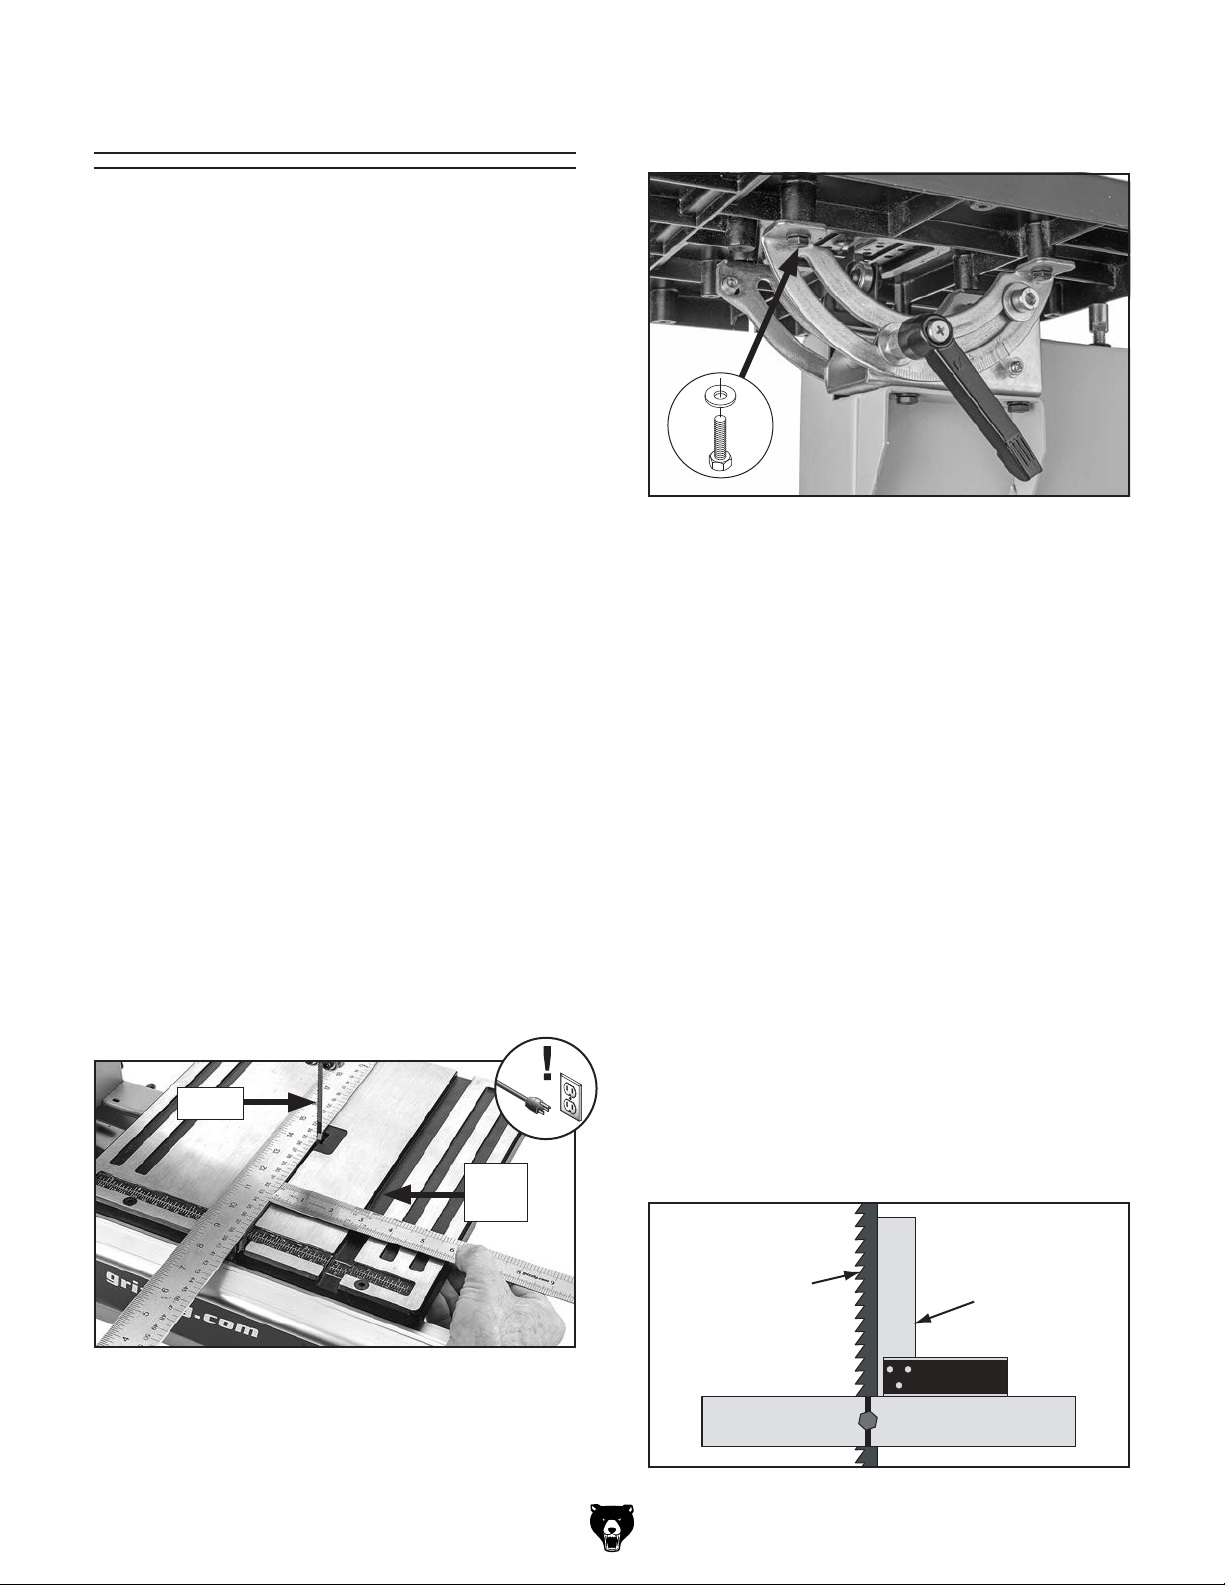
Place straightedge along blade so it barely
3.
touches both front and back of blade without
going across a tooth (see Figure
.................................................. 1
.............................................. 1
................................... 1
Adusting Miter Slot Parallelism
32).
5. Loosen trunnion hex bolts that secure table
(see Figure
x 4
Figure 33. Location of trunnion hex bolts.
6.
Adjust table until distance between straight-
edge and miter slot is same at front and back
of table.
Taking care not to move table, tighten trun-
7.
nion hex bolts, then repeat Step
adjustment.
33).
4 to verify
Measure distance between straightedge and
4.
miter slot (see Figure
be same at front and back of table.
— If distance is same at front and back of
table, no adjustment is necessary.
— If distance is not same at front and back
of table, it must be adjusted; proceed to
Step 5.
Blade
32). Distance should
Miter
Slot
Adjusting Table Perpendicular to
Blade
1. DISCONNECT MACHINE FROM POWER!
Place a square on table and against back
2.
of blade, as illustrated in Figure 34. Table
should be perpendicular to back of blade.
— If the table is perpendicular to the back
of the blade, no adjustment is necessary;
proceed to Aligning Fence on Page 28.
— If the table is not perpendicular to the back
of the blade, you must shim the table; proceed to Step 3.
Blade
Square
Figure 32. Example of placing a straightedge
along blade and measuring to miter slot.
Model G0948 (Mfd. Since 08/21)
Table
Figure 34. Squaring back of blade and table.
-27-
Page 31
3. Determine which trunnion is on low side
of table, then remove two hex bolts (see
Figure
Insert a shim, such as a thin washer, between
4.
table and low trunnion at each mounting
location.
Re-install and tighten trunnion hex bolts, then
5.
repeat Step 2 to verify adjustment.
33 on Page 26) from low trunnion.
Aligning Fence
Aligning Fence
3.
Install fence on right side of blade, aligned
with edge of miter slot, then lock it in place.
— If fence is parallel with miter slot, no
adjustment is necessary.
— If fence is not parallel with miter slot, pro-
ceed to Step 4.
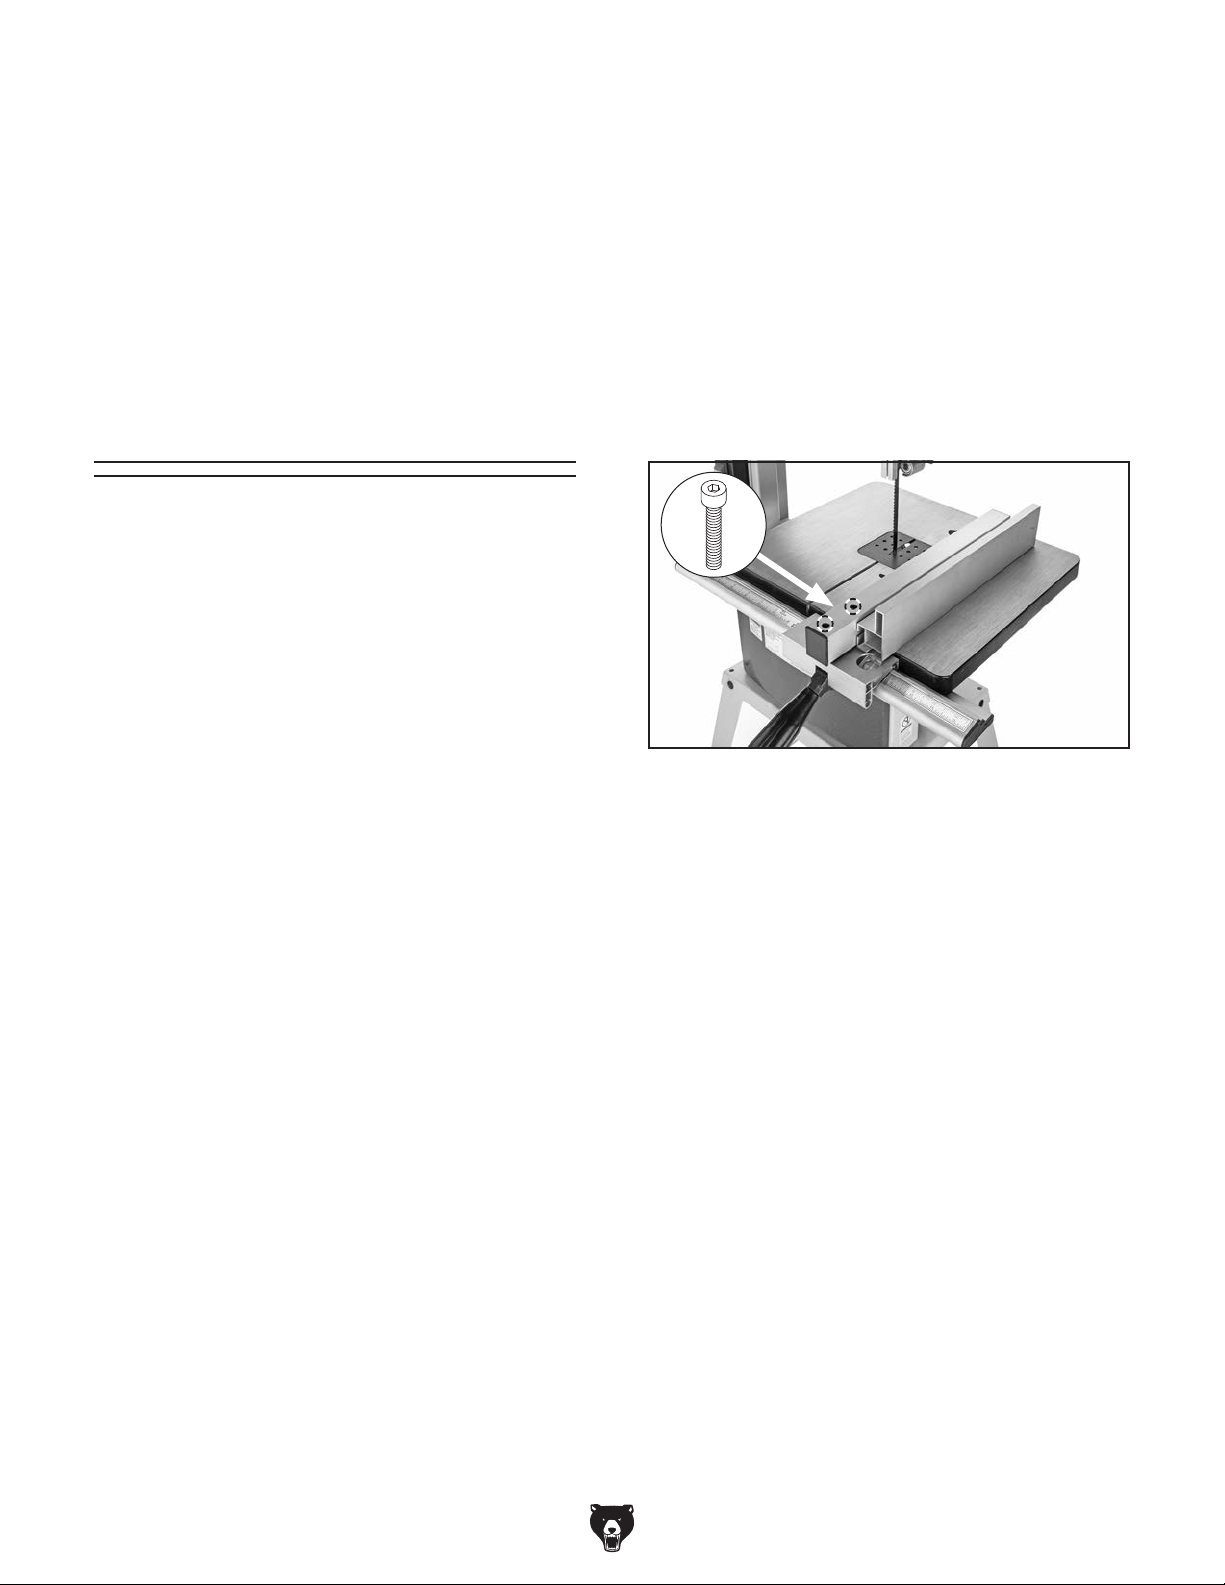
. Loosen (2) fence adjustment cap screws
4
Figure 35), adjust fence parallel with
(see
miter slot, then tighten cap screws to secure
setting.
To ensure cutting accuracy, the fence should be
aligned parallel with the blade. This is achieved by
aligning the fence with the miter slot.
Occasionally, even after aligning the fence,
Note:
a symptom known as "blade lead" will develop,
requiring the fence to be skewed slightly to
compensate for the blade lead problem. Refer
to Blade Lead, beginning on
information on blade lead and skewing the fence.
Item(s) Needed Qty
Hex Wrench 4mm .............................................. 1
To align fence:
DISCONNECT MACHINE FROM POWER!
1.
2. Make sure table is aligned with blade (see
Adjusting Miter Slot Parallelism on Page 27
for instructions).
Page 56 for more
x 2
Figure 35. Location of fence adjustment cap
screws.
-28-
Model G0948 (Mfd. Since 08/21)
Page 32
Calibrating
Miter Gauge
The miter gauge needs to be calibrated to the
blade when it is first mounted in the miter slot.
Tool(s) Needed Qty
Phillips Screwdriver #2 ...................................... 1
Square
To calibrate miter gauge:
............................................................... 1
1. DISCONNECT MACHINE FROM POWER!
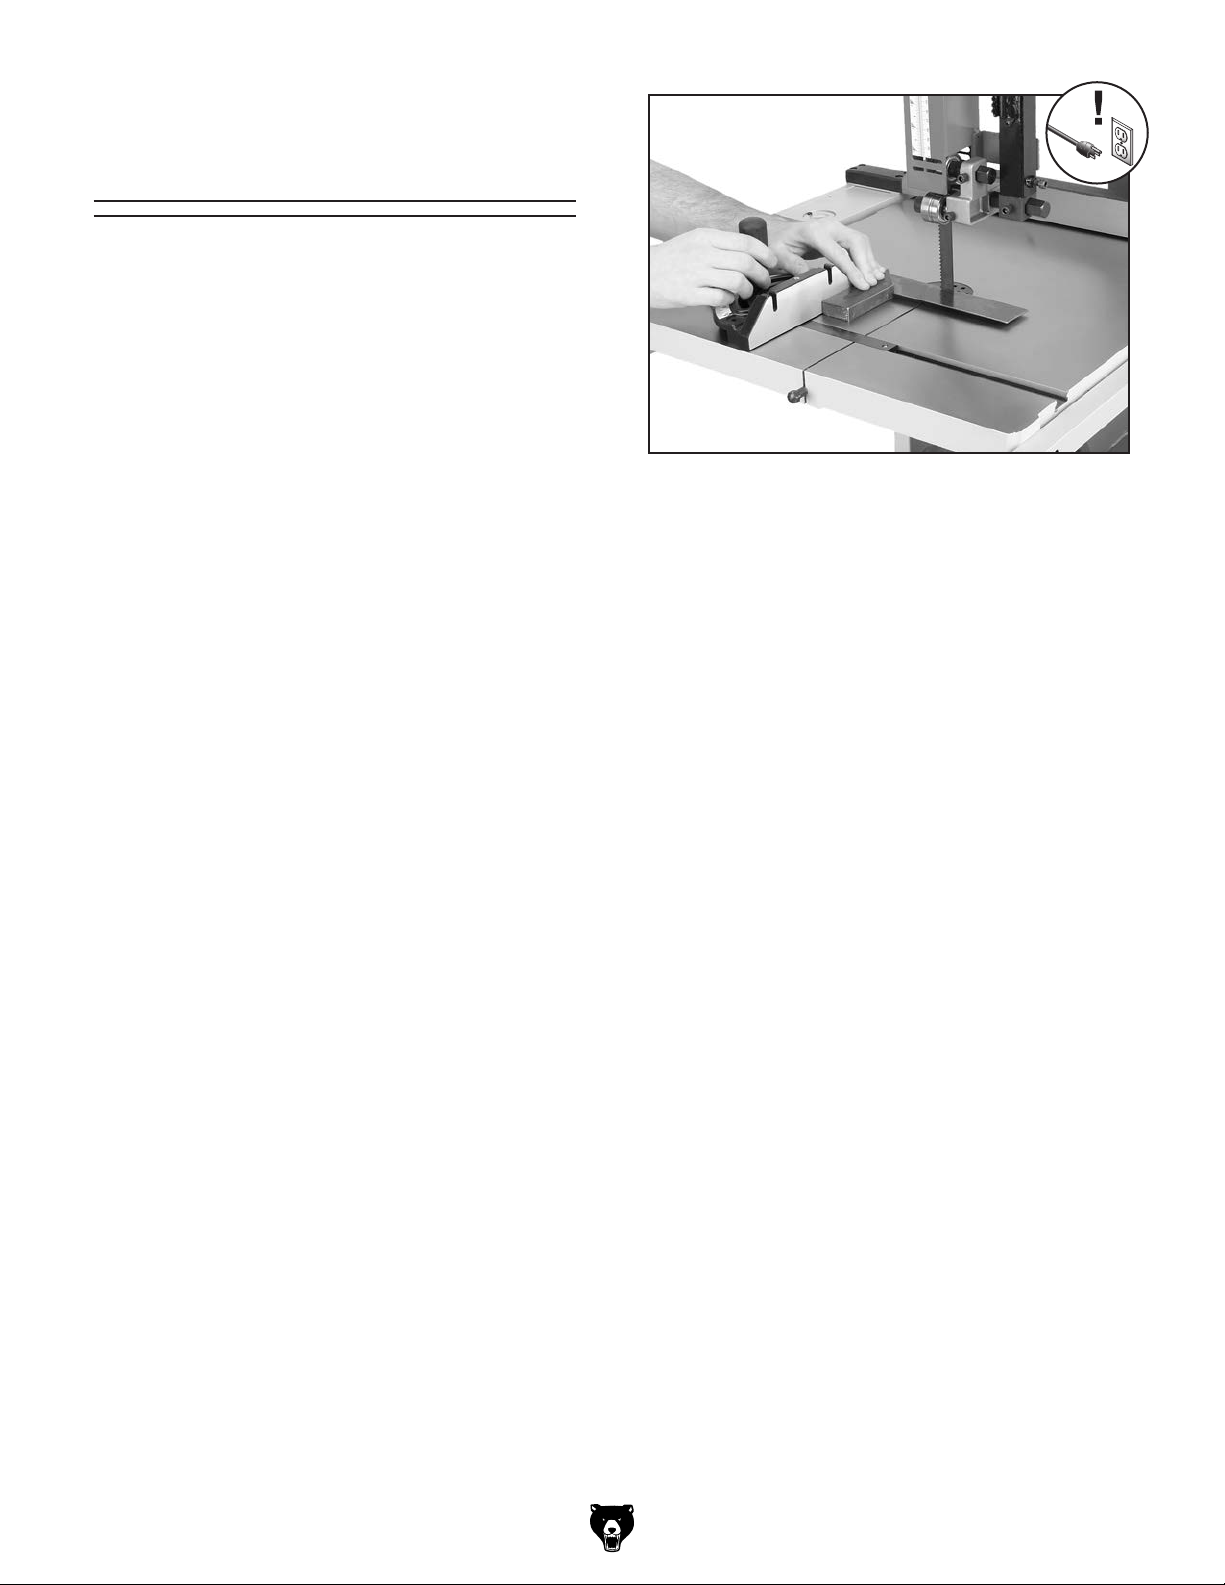
2. Place one edge of square against face of
miter gauge and other edge of square against
side of blade, as shown in Figure 36.
Note: Make sure square does not go across
a blade tooth when performing this step.
— If square rests flush and evenly against
both miter gauge face and side of blade,
then no adjustments are necessary.
— If square does not rest flush and evenly
against both miter gauge face and side of
blade, the miter gauge must be calibrated.
Proceed to Step 3.
Figure 36. Example of squaring miter gauge to
blade.
Loosen lock knob on miter gauge and adjust
3.
face flush with edge of square.
Tighten lock knob, and verify square rests
4.
flush and evenly against both miter gauge
face and side of blade.
Note: Sometimes the tightening procedure
can affect the adjustment.
Loosen screw that secures angle pointer,
5.
adjust pointer to 0° mark on scale, then
tighten screw to secure setting.
Model G0948 (Mfd. Since 08/21)
-29-
Page 33
SECTION 4: OPERATIONS
The purpose of this overview is to provide the novice machine operator with a basic understanding
of how the machine is used during operation, so
the
discussed later
in this manual
Due to the generic nature of this overview, it is
not intended to be an instructional guide. To learn
more about specific operations, read this entire
manual,
training from experienced
machine operators
outside of this manual by reading "how-to" books,
trade magazines, or websites.
To reduce your risk of
serious injury, read this
entire manual BEFORE
To reduce risk of eye injury from flying
Operation Overview
machine controls/components
are easier to understand.
To complete a typical operation, the operator
does the following:
Examines workpiece to make sure it is suit-
1.
able for cutting.
Adjusts table tilt, if necessary, to correct
2.
angle of desired cut.
If using fence, adjusts it for width of cut and
3.
then locks it in place. If using miter gauge,
adjusts angle and locks it in place.
seek additional
, and do additional research
using machine.
chips or lung damage from breathing dust,
always wear safety glasses and a respirator
when operating this machine.
Loosens guide post lock knob, adjusts
4.
the upper blade guide height to just clear
workpiece (no more than
ens guide post lock knob.
Checks to make sure workpiece can safely
5.
pass all the way through blade without interference from other objects.
Puts on safety glasses and a respirator.
6.
7. Starts dust collector, then bandsaw.
8. Holds workpiece firmly and flatly against both
table and fence (or miter gauge), and then
pushes workpiece into blade at a steady and
controlled rate until cut is complete.
The operator is very careful to keep fingers
away from blade and uses a push stick to
feed narrow workpieces.
Stops bandsaw, then dust collector.
9.
1
⁄4"), then re-tight-
If you are not experienced with this type
of machine, WE STRONGLY RECOMMEND
that you seek additional training outside of
this manual. Read books/magazines or get
formal training before beginning any projects. Regardless of the content in this section, Grizzly Industrial will not be held liable
for accidents caused by lack of training.
-30-
Model G0948 (Mfd. Since 08/21)
Page 34
Basic Functions
Workpiece
of a Bandsaw
A properly adjusted bandsaw can be safer to
operate than most other saws and performs many
types of cuts with ease and accuracy. It is capable
of performing the following types of cuts:
Straight Cuts
• Miters
• Angles
• Compound Angles
• Resawing
• Ripping
• Crosscutting
Irregular Cuts
• Simple and Complex Curves
• Duplicate Parts
• Circles
• Beveled Curves
Basic Cutting Tips
Here are some basic tips to follow when operating the bandsaw:
Inspection
Some workpieces are not safe to cut or may
require modification before they are safe to cut.
Before cutting, inspect all workpieces for the
following:
• Material Type: This machine is intended for
cutting natural and man-made wood products, laminate covered wood products, and
some plastics. Cutting drywall or cementious
backer board creates extremely fine dust
and may reduce the life of the bearings. This
machine is NOT designed to cut metal, glass,
stone, tile, etc.; cutting these materials with a
table saw may lead to injury.
• Foreign Objects: Nails, staples, dirt, rocks
and other foreign objects are often embedded in wood. While cutting, these objects
can become dislodged and hit the operator,
cause kickback, or break the blade, which
might then fly apart. Always visually inspect
your workpiece for these items. If they can't
be removed, DO NOT cut the workpiece.
• Replace, sharpen, and clean blades often
for best performance. Check guides, tension, and alignment settings periodically and
adjust when necessary to keep the saw running in top condition.
• Use light and even pressure while cutting.
Light feeding pressure makes it easier to cut
straight and prevents undue friction or strain
on the bandsaw components and the blade.
• Avoid twisting the blade when cutting around
tight corners. Allow the blade to saw its way
around the corners. Always use relief cuts
when possible.
• Misusing the saw or using incorrect techniques (e.g. twisting the blade with the
workpiece, incorrect feed rate, etc.) is unsafe
and results in poor cuts.
• Large/Loose Knots: Loose knots can
become dislodged during the cutting operation. Large knots can cause kickback and
machine damage. Choose workpieces that
do not have large/loose knots or plan ahead
to avoid cutting through them.
• Wet or "Green" Stock: Cutting wood with a
moisture content over 20% causes unnecessary wear on the blades, increases the risk of
kickback, and yields poor results.
• Excessive Warping: Workpieces with excessive cupping, bowing, or twisting are dangerous to cut because they are unstable and
often unpredictable when being cut. DO NOT
use workpieces with these characteristics!
• Minor Warping: Workpieces with slight cupping can be safely supported if the cupped
side is facing the table or the fence. On
the contrary, a workpiece supported on the
bowed side will rock during a cut and could
cause kickback or severe injury.
Model G0948 (Mfd. Since 08/21)
-31-
Page 35
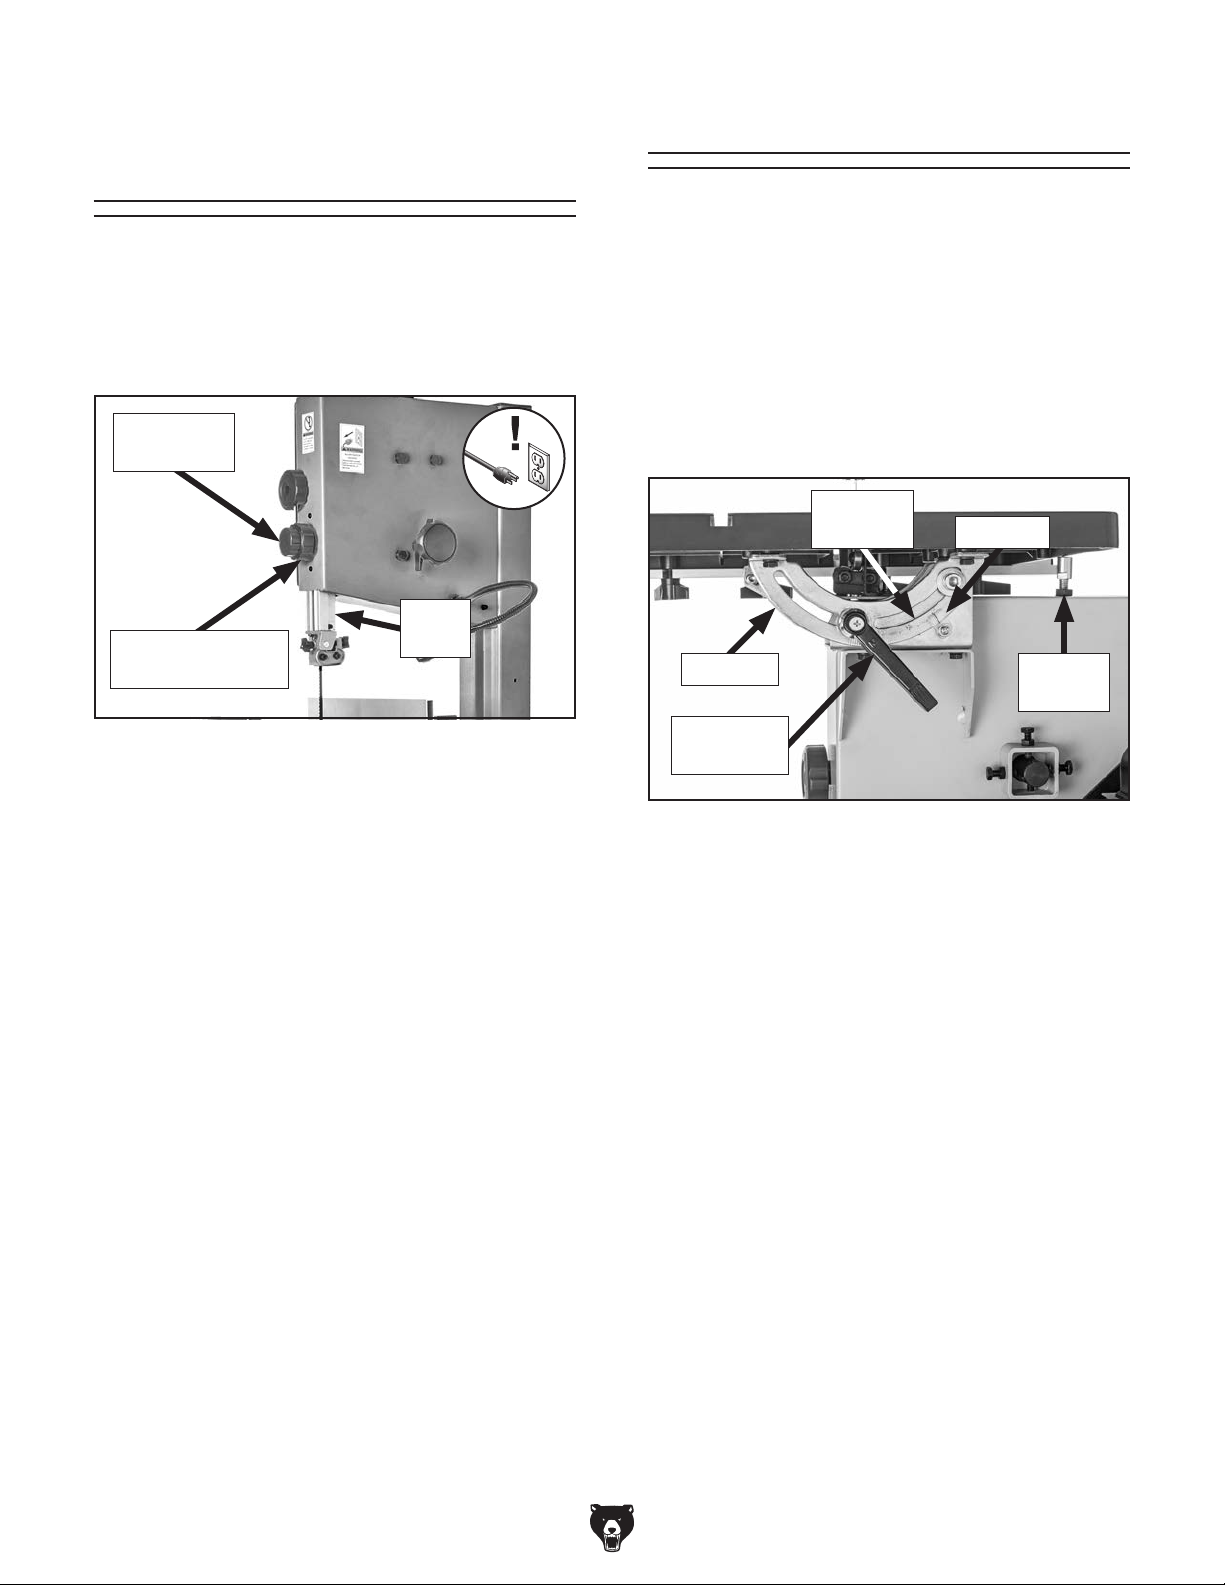
Setting Upper Blade
Guide Height
When cutting, the blade guides must always be
positioned so they just clear (no more than
workpiece. The guide post, shown in
allows the upper blade guide assembly to be
quickly adjusted for height.
Guide Post
Lock Knob
Guide
Guide Post
Adjustment Knob
Post
1
⁄4") the
Figure 37,
Tilting Table
The table can be tilted from 0°–45° right to make
beveled cuts. A table tilt scale with indicator is
provided on the trunnion, and a positive stop is
provided for quickly returning the table back to 0°
from a right-tilt setting (see
Note: The tilt scale on the trunnion serves as a
guide only. For more accurate results, use a bevel
gauge or protractor to set the desired table tilt relative to the blade.
Table Tilt
Scale
Trunnion
Figure 38).
Indicator
Positive
Stop
Figure 37. Guide post controls.
To adjust height of upper blade guides:
DISCONNECT MACHINE FROM POWER!
1.
Loosen guide post lock knob.
2.
3. Using guide post adjustment knob, position
guide post so that blade guide assembly just
clears (no more than
Tighten guide post lock knob to secure
4.
setting.
1
⁄4") workpiece.
Table Tilt
Lock Lever
Figure 38. Table tilt controls.
Tilting Table
DISCONNECT MACHINE FROM POWER!
1.
Loosen table tilt lock lever (see Figure 38).
2.
Tilt table to desired angle, then tighten lock
3.
lever.
-32-
Model G0948 (Mfd. Since 08/21)
Page 36
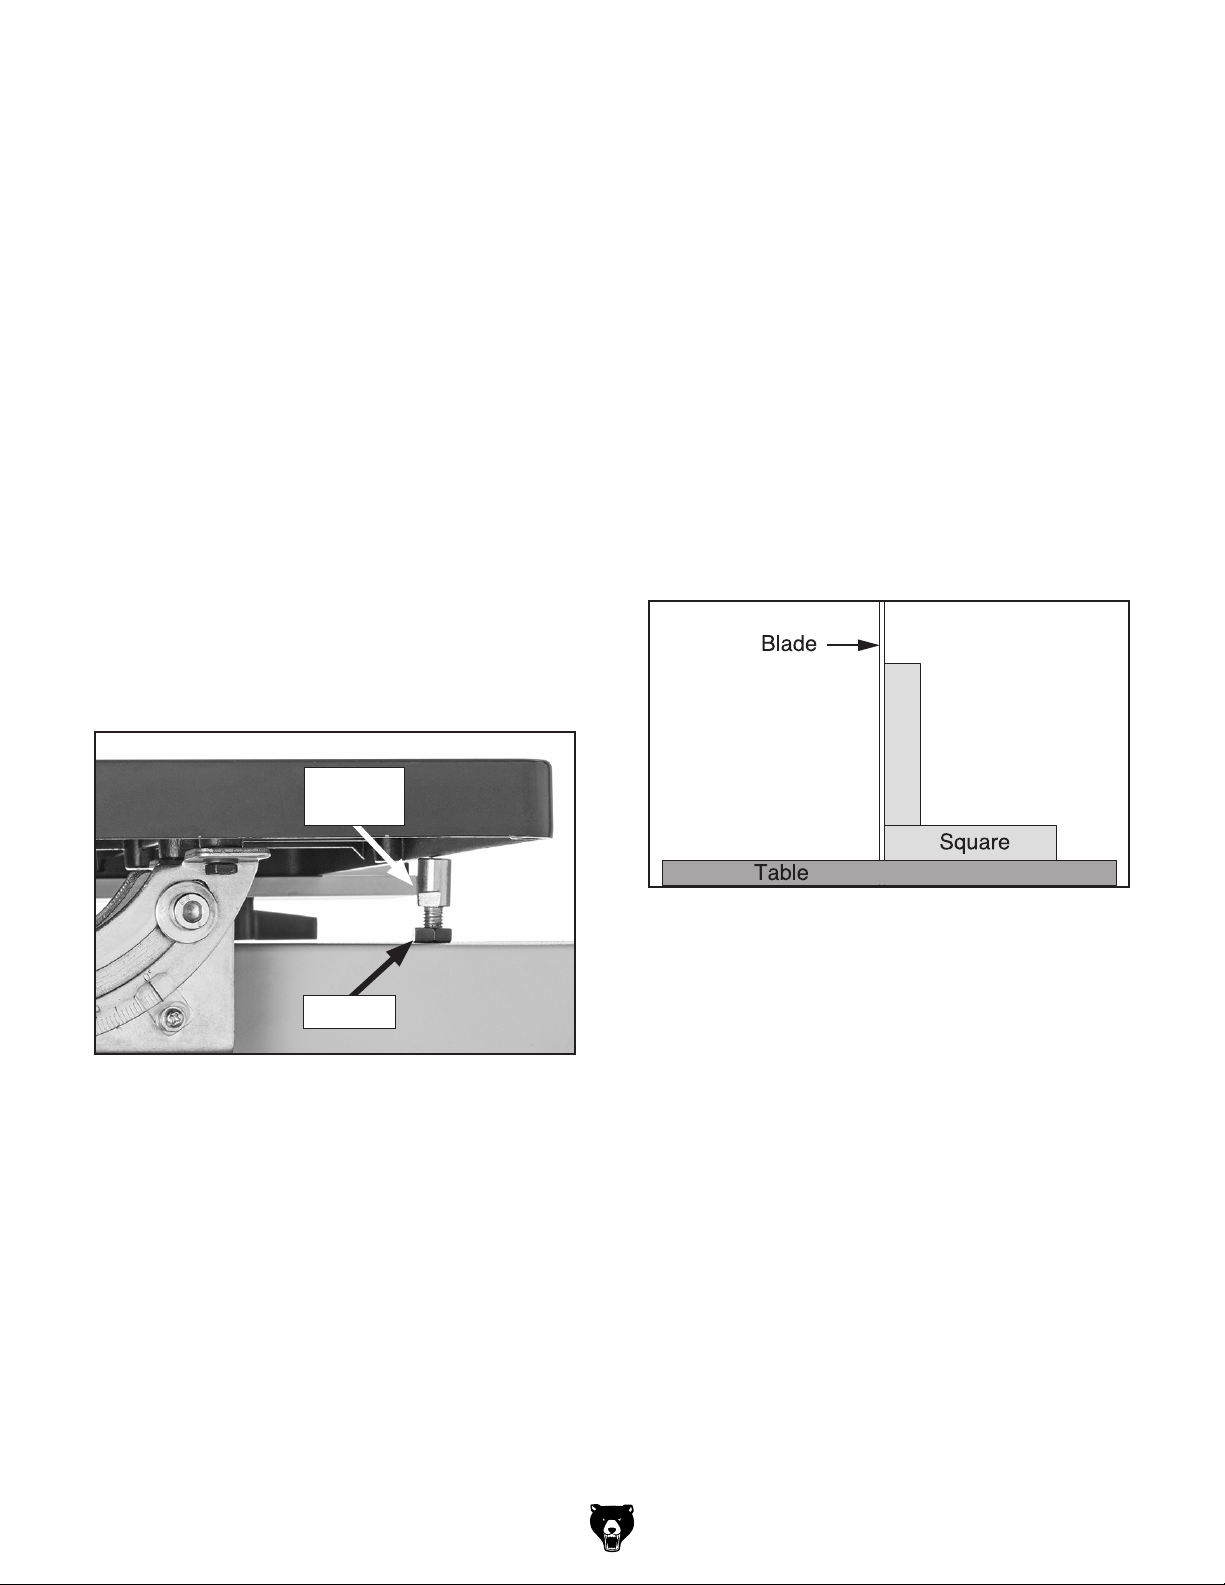
Using Positive Stop
Tool(s) Needed Qty
Open-End Wrenches 10, 14mm ..................1 Ea.
The positive stop (see Figure 39) allows you to
quickly return the table to 0° from a right-tilt setting. The positive stop is adjustable, allowing for
calibration, or if desired, minor deviations from 0°.
To use positive stop:
DISCONNECT MACHINE FROM POWER!
1.
Loosen table tilt lock lever (see Figure 38 on
2.
Page 32).
Tilt table to desired angle, then secure posi-
3.
tion by tightening table tilt lock lever (see
Figure 38 on Page 32).
Loosen jam nut on stop bolt (see Figure 39),
4.
and turn bolt until it just touches bottom of
table.
calibrating positive stop
Checking/Calibrating Positive Stop
Tool(s) Needed Qty
Open-End Wrenches 10, 14mm ..................1 Ea.
Machinist's Square
To check/calibrate positive stop:
DISCONNECT MACHINE FROM POWER!
1.
Loosen table tilt lock lever, and tilt table to
2.
approximately 10° right.
3. Loosen positive stop jam nut, and lower posi-
tive stop bolt so it will not interfere with the
following steps.
Place a machinist's square flat on table against
4.
side of blade, as illustrated in Figure 40.
............................................ 1
Positive
Stop Bolt
Jam Nut
Figure 39. Location of positive stop bolt and jam
nut.
Tighten jam nut to secure stop bolt setting.
5.
Note: It is always a good idea to check table
tilt scale and make sure positive stop bolt is
correctly calibrated.
Figure 40. Squaring table to blade.
5.
Tilt table until it is square with blade.
Adjust positive stop bolt so it just touches
6.
bottom of table, and tighten jam nut to secure
position.
Check table to ensure it is square with blade.
7.
If necessary, repeat Step 5.
Note: If you wish to set the positive stop to an
angle other than 0°, follow Steps 1–5 for the
desired angle.
Loosen screw on table tilt scale indicator,
8.
align pointer with zero on scale, then tighten
screw.
Model G0948 (Mfd. Since 08/21)
-33-
Page 37
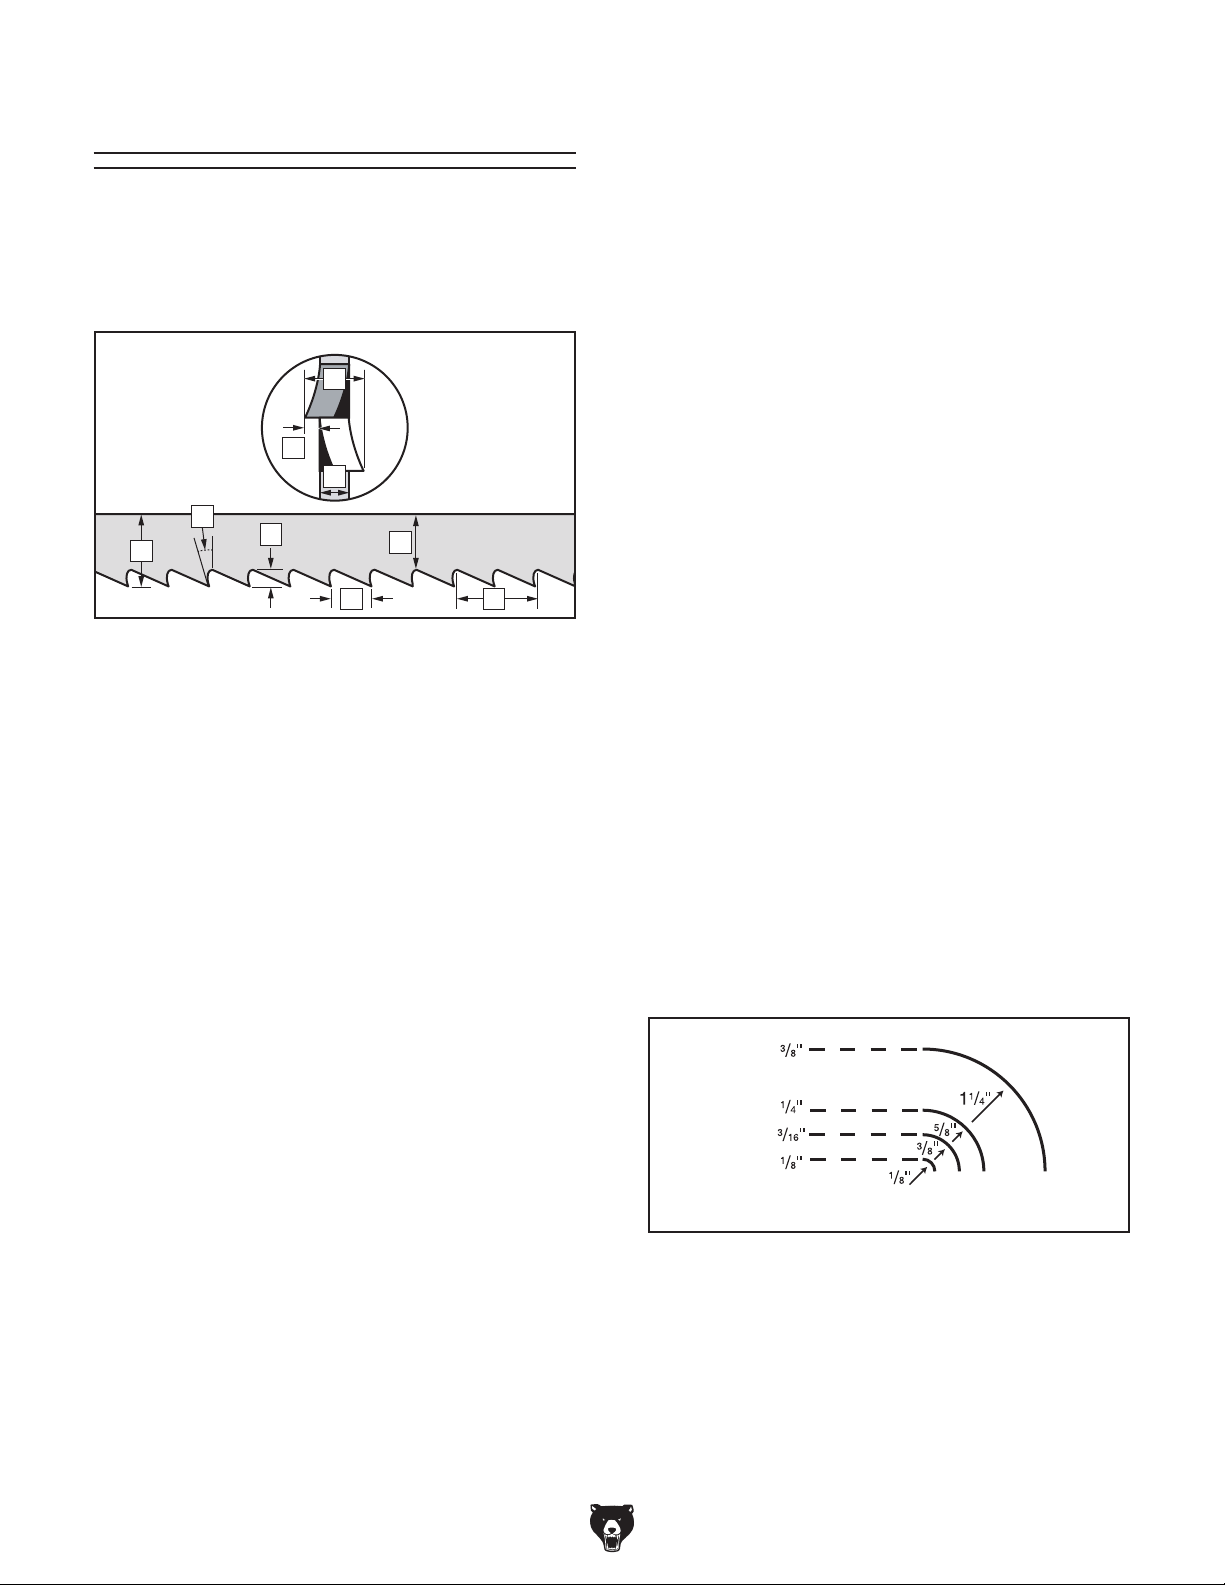
Choosing Blades
Selecting the right blade requires a knowledge
of the various blade characteristics to match the
blade with the particular cutting operation.
Blade Terminology
A
B
C
E
D
Figure 41. Bandsaw blade components.
A. Kerf: The amount of material removed by the
blade during cutting.
B. Tooth Set: The amount each tooth is bent
left or right along the blade.
C. Gauge: The thickness of the blade.
D. Blade Width: The widest point of the blade
measured from the tip of the tooth to the back
edge of the blade.
E. Tooth Rake: The angle of the tooth face from
a line perpendicular to the length of the blade.
F
H
G
I
Blade Dimensions
Length Range ..................................... 711⁄2 –721⁄2 "
Width Range
Selecting the right blade requires a knowledge
of the various blade characteristics to match the
blade with the particular cutting operation.
.............................................1⁄8"–1⁄2 "
Blade Length
Measured by the circumference, blade lengths
are usually unique to the brand of your bandsaw
and the distance between wheels. Blades will
vary slightly even in the same length because of
how they are welded. Refer to the Accessories
section later in this manual for blade replacements from Grizzly.
Blade Width
Measured from the back of the blade to the tip of
the blade tooth (the widest point), blade width is
often the first consideration given to blade selection. Blade width dictates the largest and smallest
curve that can be cut, as well as how accurately it
can cut a straight line.
Always pick the size of blade that best suits your
application.
• Curve Cutting: Use the chart in Figure 42 to
determine the correct blade for curve cutting.
Determine the smallest radius curve that will
be cut on your workpiece and use the corresponding blade width.
F. Gullet Depth: The distance from the tooth tip
to the bottom of the curved area (gullet).
G. Tooth Pitch: The distance between tooth
tips.
H. Blade Back: The distance between the bot-
tom of the gullet and the back edge of the
blade.
I. TPI: The number of teeth per inch measured
from gullet to gullet.
-34-
Blade Width
Cutting Radius
Figure 42. Recommended cutting radius per
blade width.
• Straight Cutting: Use the largest width
blade that you own. Large blades excel at
cutting straight lines and are less prone to
wander.
Model G0948 (Mfd. Since 08/21)
Page 38
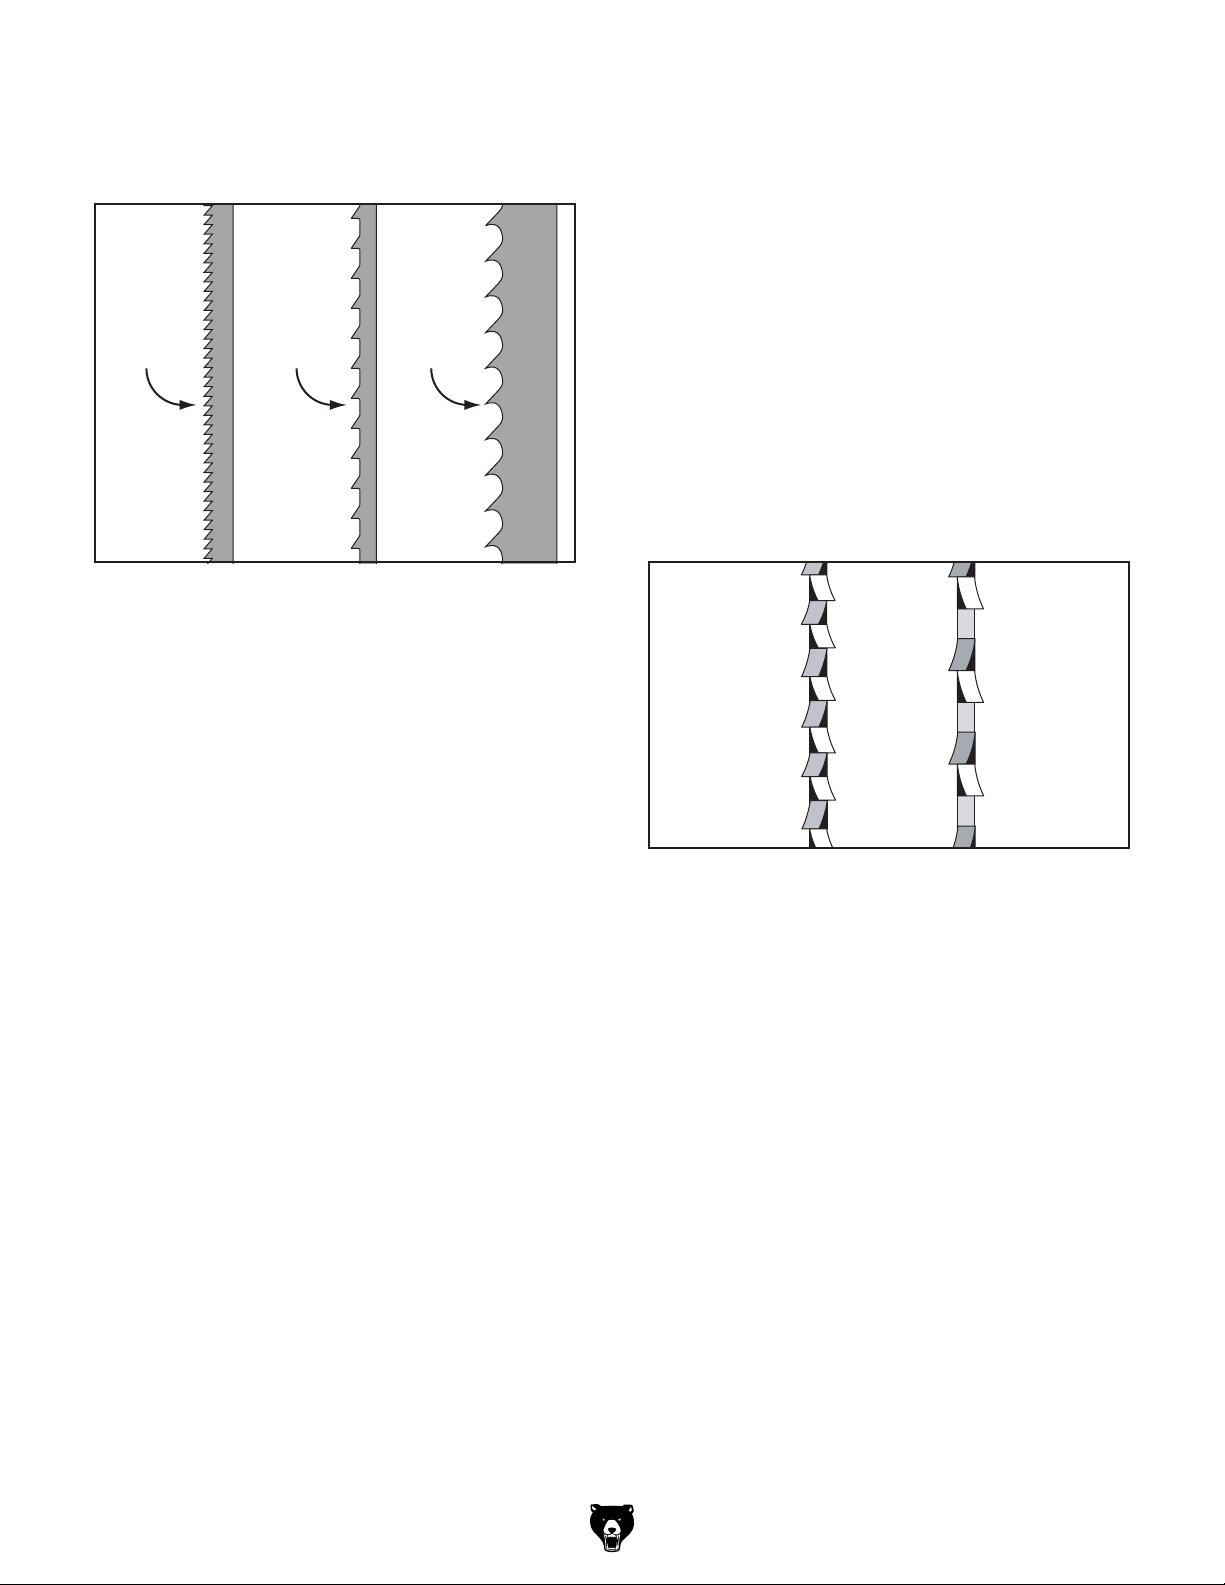
Tooth Style
Figure 43 illustrates the three main blade tooth
styles:
Raker Skip Hook
Figure 43. Main blade tooth styles.
• Raker: Considered to be the standard
because the tooth size and shape are the
same as the tooth gullet. The teeth on raker
blades usually are very numerous, have no
angle, and produce cuts by scraping the
material. As a result, smooth cuts can be
achieved without cutting fast or generating
more heat than other tooth types.
Tooth Pitch
Measured as TPI (teeth per inch), tooth pitch
determines the number of teeth. More teeth per
inch (fine pitch) will cut slower, but smoother; while
fewer teeth per inch (coarse pitch) will cut rougher,
but faster. As a general rule, choose blades that
will have at least three teeth in the material at all
times. Use fine-pitched blades on harder woods
and coarse-pitched blades on softer woods.
Tooth Set
Two common tooth sets for wood bandsaw blades
are alternate and raker. Each different type of
tooth set removes material in a different manner,
leaving cuts with different characteristics (see
Figure 44).
Alternate Raker
• Skip: Similar to a raker blade that is missing
every other tooth. Because of the design,
skip toothed blades have a much larger gullet
than raker blades, and therefore, cut faster
and generate less heat. However, these
blades also leave a rougher cut than raker
blades.
• Hook: The teeth have a positive angle (downward) which makes them dig into the material,
and the gullets are usually rounded for easier
waste removal. These blades are excellent
for the tough demands of resawing and ripping thick material.
Figure 44. Common woodcutting bandsaw blade
tooth sets.
• Alternate: An all-purpose arrangement
where the teeth are bent evenly left and right
of the blade.
• Raker: Three teeth in a recurring group—one
bent left, one bent right, and then one that is
not bent. The raker set is ideal for most contour cuts.
Model G0948 (Mfd. Since 08/21)
-35-
Page 39
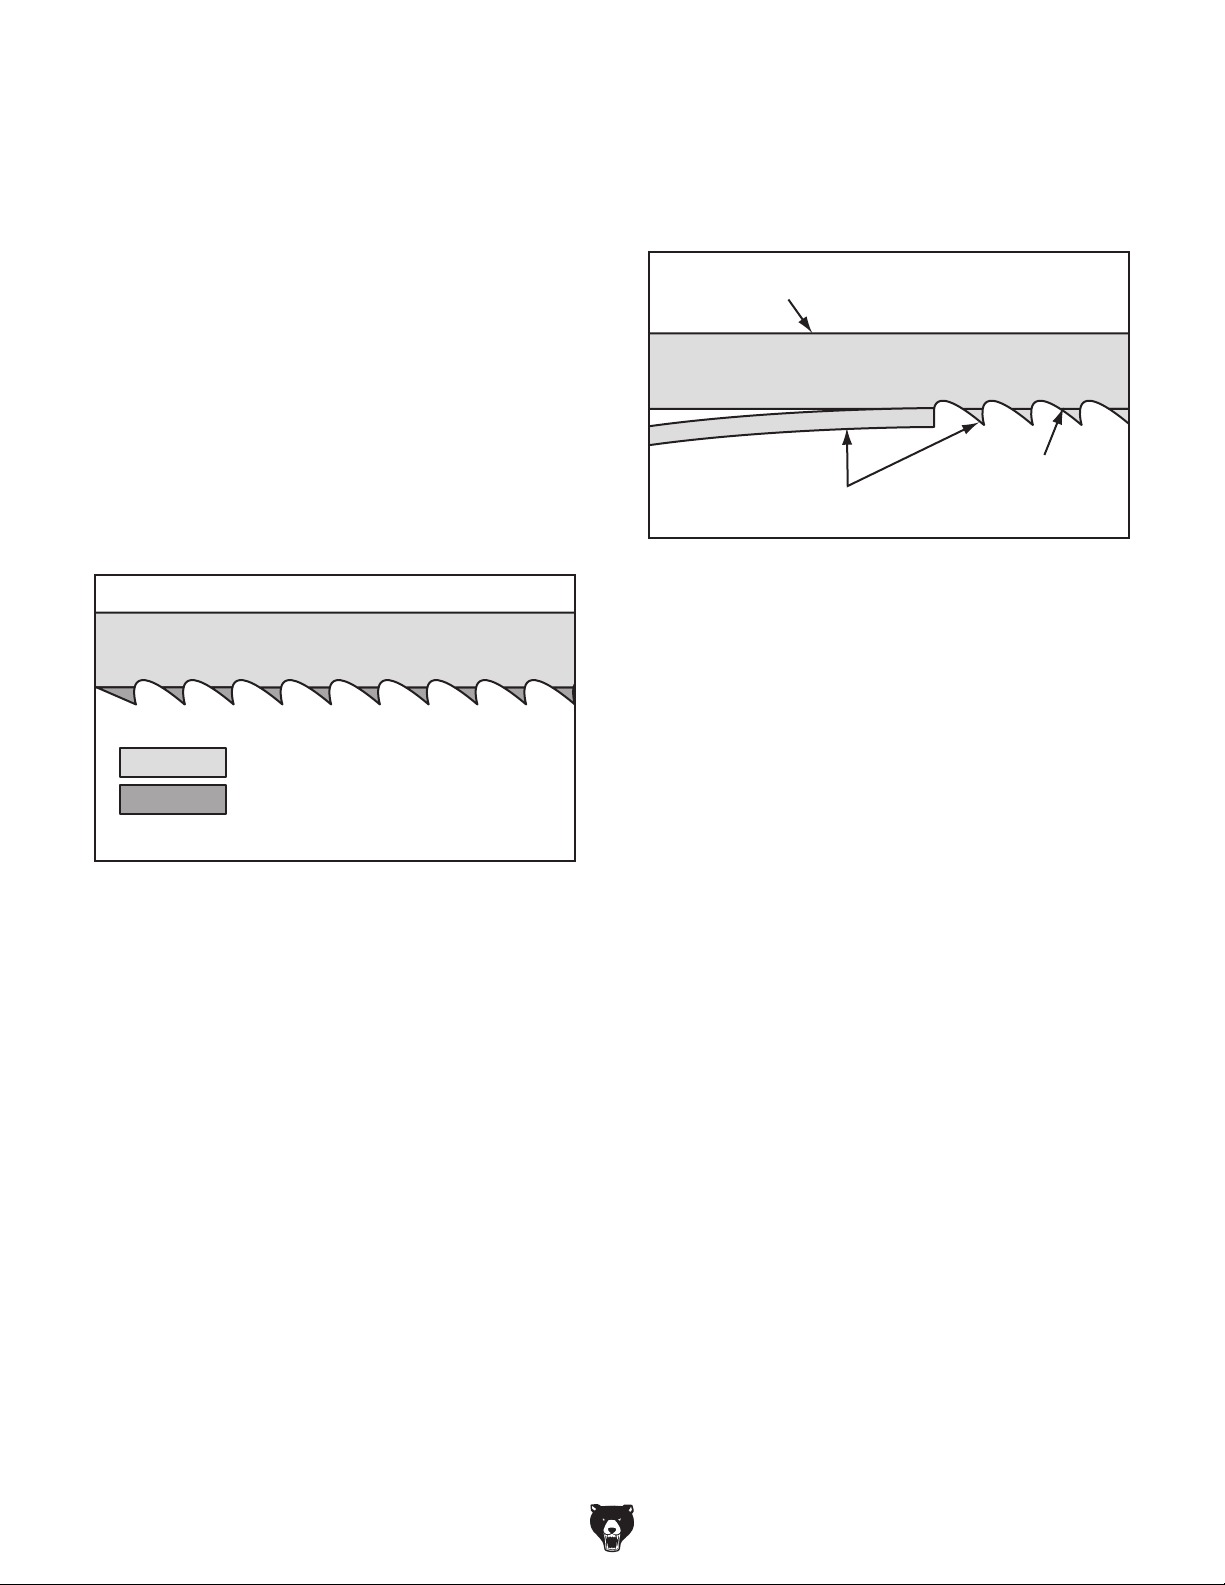
Blade Material
Bandsaw blades must meet two requirements:
flexibility and hardness. The flexibility of a blade
allows it to travel on the wheel as a band, while
hardness allows the teeth to cut and hold an
edge. Modern materials technology has allowed
bandsaw blades to meet these requirements in
various ways.
Carbon Steel: These blades are differentially
heat treated to provide hard teeth that will hold an
edge, and yet be flexible in the back.
Bi-metal Blade: A strip of high-speed tool steel is
precision welded to a flexible carbon blade, then
teeth are ground into the blade to provide good
edge-holding qualities for blades taking a lot of
abuse (see Figure 46).
Carbon Steel Blade
Carbide Tooth: Extremely hard carbide is either
welded onto or impregnated into the carbon steel
blades, providing superior edge-holding characteristics (see Figure 45).
Carbon Steel
Carbide Impregnated Steel
Figure 45. Carbide-tooth blade composition.
Weld
High-Speed Steel
Figure 46. Bi-metal blade composition.
-36-
Model G0948 (Mfd. Since 08/21)
Page 40
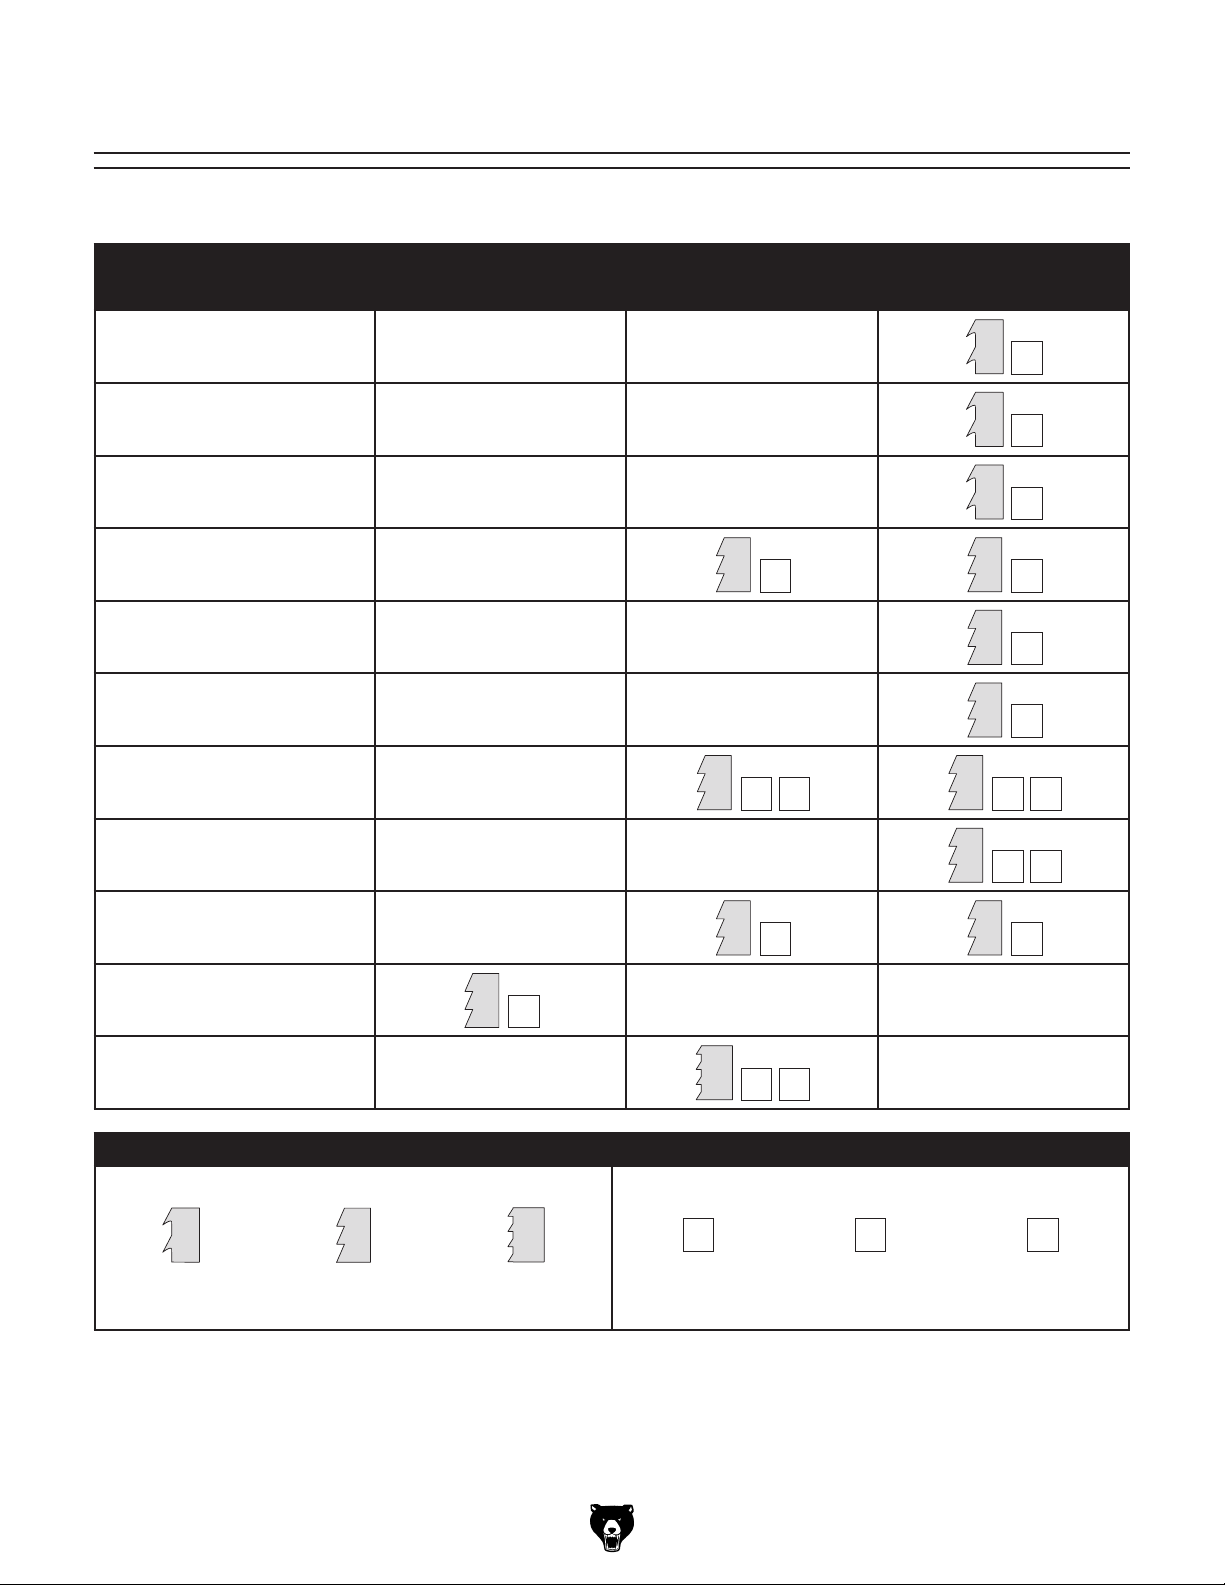
Blade Selection Chart
H
H
H
H
H
H
H
H
H
H
R
H
H
R
H
Use the blade selection chart below as a general guide when selecting a blade for your operation.
Cutting Operation
Resawing
Ripping Thin Stock
Ripping Thick Stock
Ripping Round Stock
Crosscutting Thin Stock
Crosscutting Thick Stock
Crosscutting Round Stock
Narrow (
Blade Width
1
⁄8" –1⁄4") Medium (3⁄16"– 1⁄2") Wide (1⁄2"– 3⁄4")
H
C
H
M
H
C
R
R
F
M
M
R
R
R
R
F
M
F
M
M
Miter Cut
Tenons
Sharp Curves
Gradual Curves
Tooth Typ e Tooth Pitch (Teeth Per Inch or TPI)
H
Hook Raker Skip
R
R
R
R
M
F
S
S
Key
F M C
Fine
(14-32 TPI)
F
M
Medium
(4-12 TPI)
F
R
M
Coarse
(2-4 TPI)
M
Model G0948 (Mfd. Since 08/21)
-37-
Page 41
Blade Care
& Break-In
Blade Care
A bandsaw blade is a thin piece of steel that is
subjected to tremendous strain. You can obtain
longer use from a bandsaw blade if you give it fair
treatment and always use the appropriate feed
rate for your operation.
Be sure to select blades with the proper width,
set, type, and pitch for each application. Using the
wrong blade will produce unnecessary heat and
shorten the life of the blade.
Blade Breakage
Many conditions may cause a bandsaw blade to
break. Blade breakage is unavoidable in some
cases, since it is the natural result of the peculiar
stresses that bandsaw blades are subjected to.
Blade breakage is also due to avoidable circumstances. Avoidable blade breakage is most often
the result of poor care or judgement on the part
of the operator when mounting or adjusting the
blade or support guides.
The most common causes of blade breakage
are:
A clean blade will perform much better than a dirty
blade. Dirty or gummed up blades pass through
the cutting material with much more resistance
than clean blades. This extra resistance also
causes unnecessary heat.
Blade Break-In
The tooth tips and edges of a new blade are
extremely sharp, and cutting at too fast of a feed
rate fractures the beveled edges of the teeth and
causes premature blade wear.
To properly break in a new blade:
Choose correct speed for blade and material
1.
of operation.
Reduce feed pressure by half for first
2.
50–100 in2 of material cut.
To avoid twisting blade when cutting, adjust
3.
feed pressure when total width of blade is in
cut.
• Faulty alignment or adjustment of the blade
guides.
• Forcing or twisting a wide blade around a
short radius.
• Feeding the workpiece too fast.
• Dull or damaged teeth.
• Over-tensioned blade.
• Upper blade guide assembly set too high
above the workpiece. Adjust the top blade
guide assembly so that there is approximate-
1
⁄8"– 1⁄4" between the bottom of the assem-
ly
bly and the workpiece.
• Using a blade with a lumpy or improperly finished braze or weld.
• Leaving the blade tensioned when not in use.
• Using the wrong pitch (TPI) for the workpiece
thickness. The general rule of thumb is to
have no less than two teeth in contact with
the workpiece at all times during cutting.
-38-
Model G0948 (Mfd. Since 08/21)
Page 42
Removing/Installing
power BEFORE changing
blade. Serious personal
injury could occur if
LACERATION HAZARD!
and difficult to handle.
while handling to reduce
Blade
Disconnect bandsaw from
machine is started during
this procedure.
Slip blade off both wheels, slide it through
7.
table slot (see
machine.
Figure 47. Example of removing blade.
Figure 47), and remove it from
Bandsaw blades are sharp
Wear heavy leather gloves
the risk of being cut.
Items Needed Qty
Heavy Leather Gloves ..................................1 Pr.
Hex Wrench 4mm
.............................................. 1
Removing Blade
1. DISCONNECT MACHINE FROM POWER!
Release blade tension by rotating blade ten-
2.
sion knob counterclockwise.
Adjust upper blade guide assembly all the
3.
way up, move blade guides completely away
from blade, and remove table insert.
Remove fence rail.
4.
Open upper and lower wheel covers.
5.
6. Put on heavy leather gloves.
Installing Blade
1. DISCONNECT MACHINE FROM POWER!
Slide blade through table slot, ensuring that
2.
teeth are pointing down toward table.
Note: If the teeth will not point downward
in any orientation, the blade is inside out.
Remove the blade and twist it right-side out.
Slip blade over wheels while making sure it
3.
is properly positioned between blade guards
and guides.
Tension blade (refer to Tensioning Blade on
4.
Page 22 for details).
Adjust blade tracking (see Initial Blade
5.
Tracking on Page 20).
Adjust upper/lower support bearings and
6.
blade guides (refer to Adjusting Blade
Support Bearings and Adjusting Blade
Guide Bearings on Pages 24–25).
Close wheel covers, and install table insert
7.
and fence rail.
Model G0948 (Mfd. Since 08/21)
Make sure fence is parallel to miter slot and,
8.
if necessary, adjust alignment (see Page 28).
-39-
Page 43
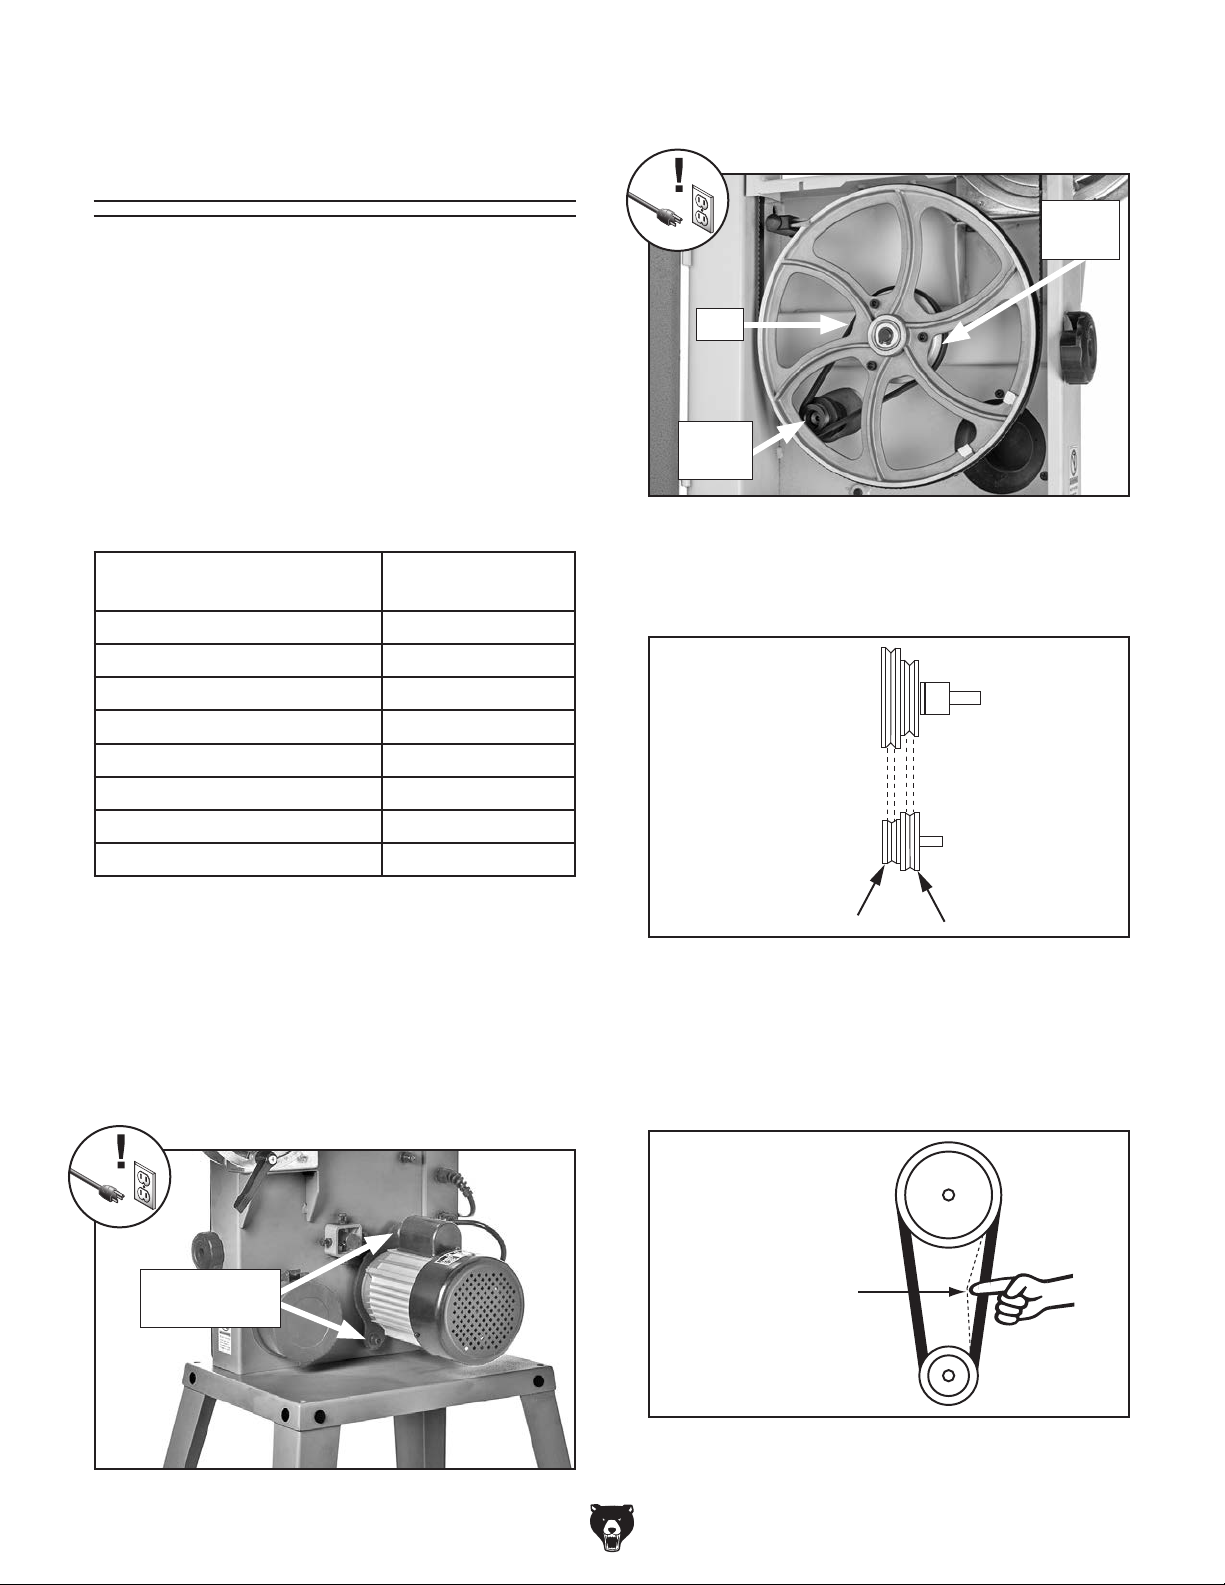
Changing
Blade Speed
The Model G0948 offers blade speeds of 1520
and 2620 FPM. Speed changes are made by repositioning the V-belt in different pulley grooves.
Keep in mind, cutting results are not just related
to blade speed. Other factors include the type of
workpiece, the blade being used for the operation,
and the feed rate.
Use the chart below as a general guide for which
blade speeds to use for various operations:
Type of Cutting Operation
General Woodworking 2620
Super Dense Hardwood 1520
Fast/Average Feed Rate 2620
Requires Slow Feed Rate 1520
Rough Edges Acceptable 2620
Requires Smooth Edges 1520
Quick, Production Cuts 2620
Detailed, Intricate Cuts 1520
Blade Speed
(FPM)
Open lower wheel cover to reveal motor pul-
3.
ley, wheel pulley, and V-belt (see Figure 49).
Wheel
Pulley
Belt
Motor
Pulley
Figure 49. Location of belt and pulleys.
4.
Position belt in pulley grooves for desired
speed (see Figure 50).
Wheel Pulley
Motor Pulley
Tool(s) Needed Qty
Hex Wrench 6mm .............................................. 1
1.
DISCONNECT MACHINE FROM POWER!
Loosen (2) motor mount cap screws (see
2.
Figure 48), and pivot motor counterclockwise
to release belt tension.
Motor Mount
Cap Screws
Figure 48. Location of motor mount cap screws.
1520 FPM
Figure 50. Belt positions on pulleys.
5.
Pivot motor clockwise. Apply pressure on
motor so there is approximately
deflection (see Figure 51), then tighten motor
mount cap screws.
Wheel Pulley
Approximately
3
/8" Deflection
Motor Pulley
Figure 51. Correct belt deflection.
6. Close lower wheel cover.
2620 FPM
3
⁄8" belt
-40-
Model G0948 (Mfd. Since 08/21)
Page 44
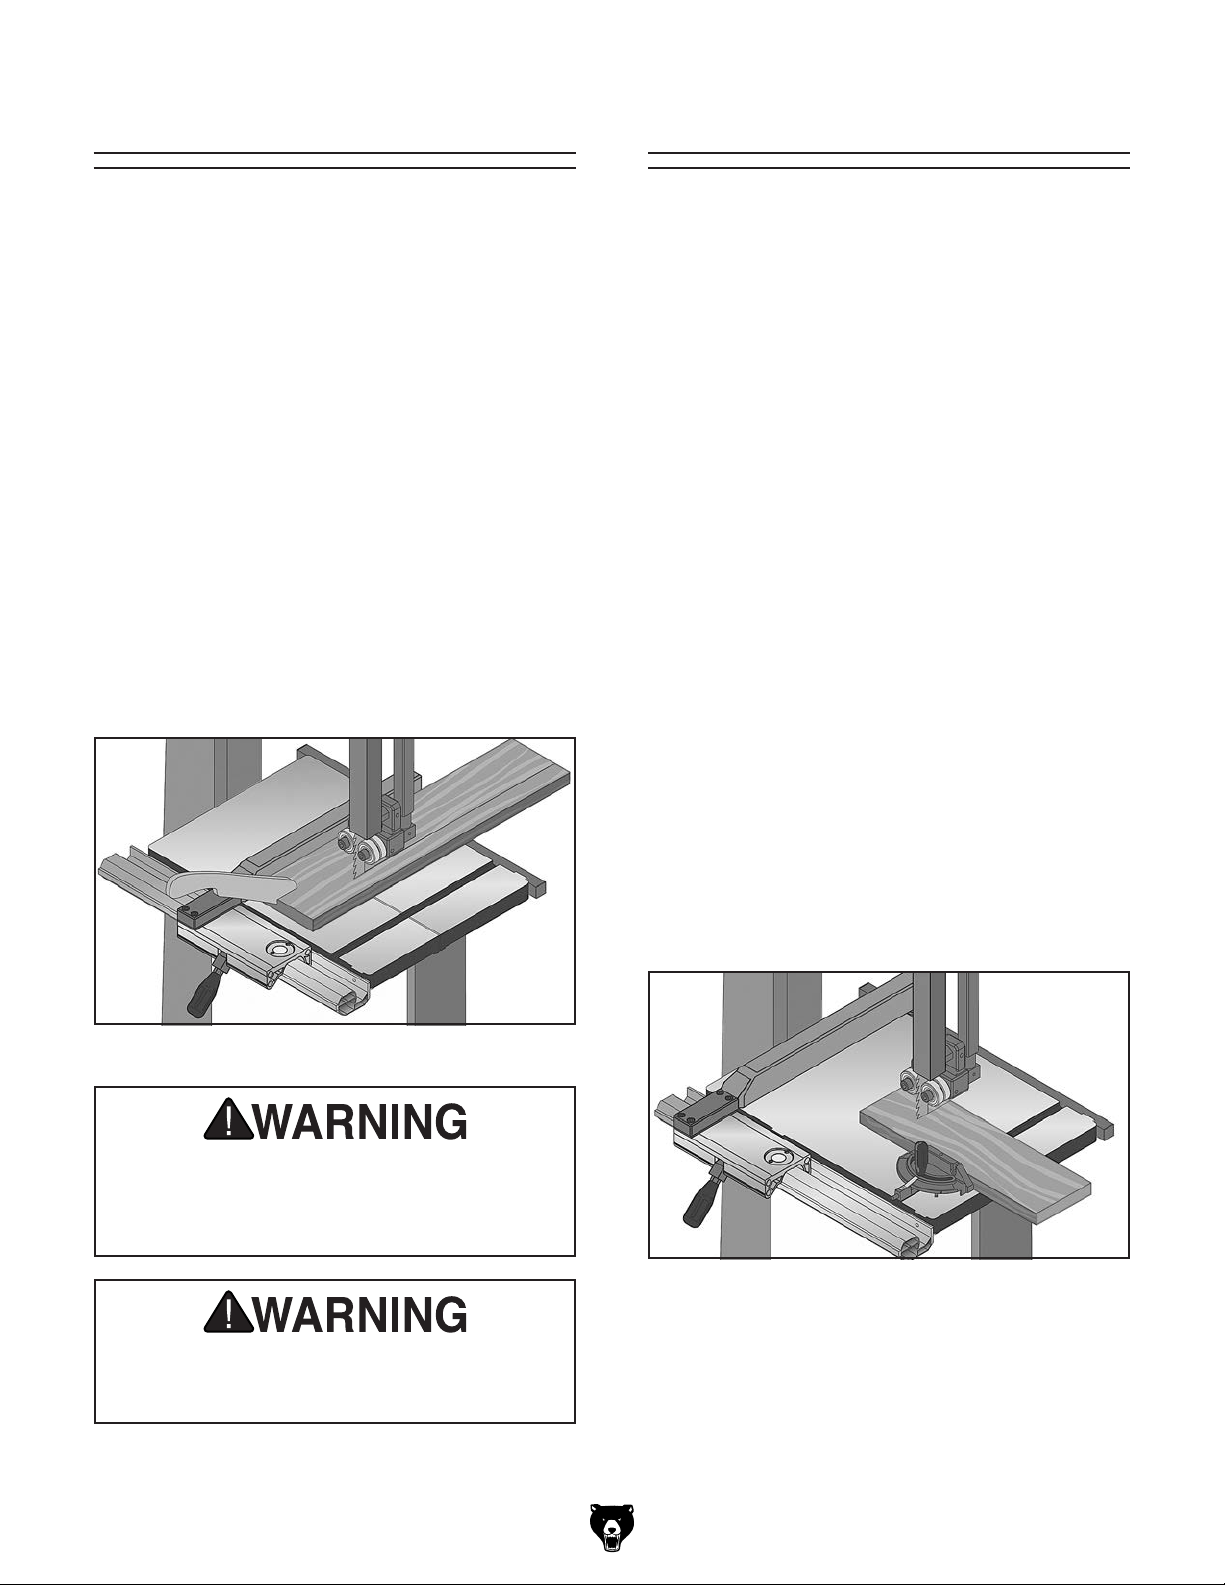
Ripping
Crosscutting
"Ripping" means cutting with the grain of the
wood stock. For plywood and other processed
wood, ripping simply means cutting down the
length of the workpiece. Beveled rip cuts may be
performed by tilting the table.
To make a rip cut:
Adjust fence to match width of cut on your
1.
workpiece, then lock fence in place.
Adjust blade guide assembly to proper height
2.
above workpiece.
After all safety precautions have been met,
3.
turn bandsaw ON and wait for it to come to
full speed. Slowly feed workpiece into blade
until blade is completely through workpiece.
Figure 52 shows an example of a ripping
operation.
Crosscutting is the process of cutting across the
grain of wood. For plywood and other processed
wood, crosscutting simply means cutting across
the width of the material. Crosscuts can be 90° or
angled using the miter gauge. Compound crosscuts are those where the miter is angled and the
table tilted.
To make a crosscut:
Mark workpiece on edge where you want to
1.
begin cut.
Adjust the blade guide assembly to the cor-
2.
rect height.
Adjust the miter gauge to the correct angle
3.
needed for cut.
Move fence out of the way. Place workpiece
4.
evenly against miter gauge, then line up mark
with blade.
Figure 52. Example of a ripping operation.
ALWAYS use a push stick when ripping
narrow pieces. Failure to follow these
warnings may result in amputation or
laceration injuries!
NEVER place fingers or hands in the line of
cut. If you slip, your hands or fingers may
go into the blade and may be cut.
After all safety precautions have been met,
5.
turn bandsaw ON and wait for it to come
to full speed. Slowly feed workpiece into
the blade until blade is all the way through
workpiece. Figure 53 shows an example of a
crosscutting operation.
Figure 53. Example of a crosscutting operation
with the miter gauge.
Model G0948 (Mfd. Since 08/21)
-41-
Page 45
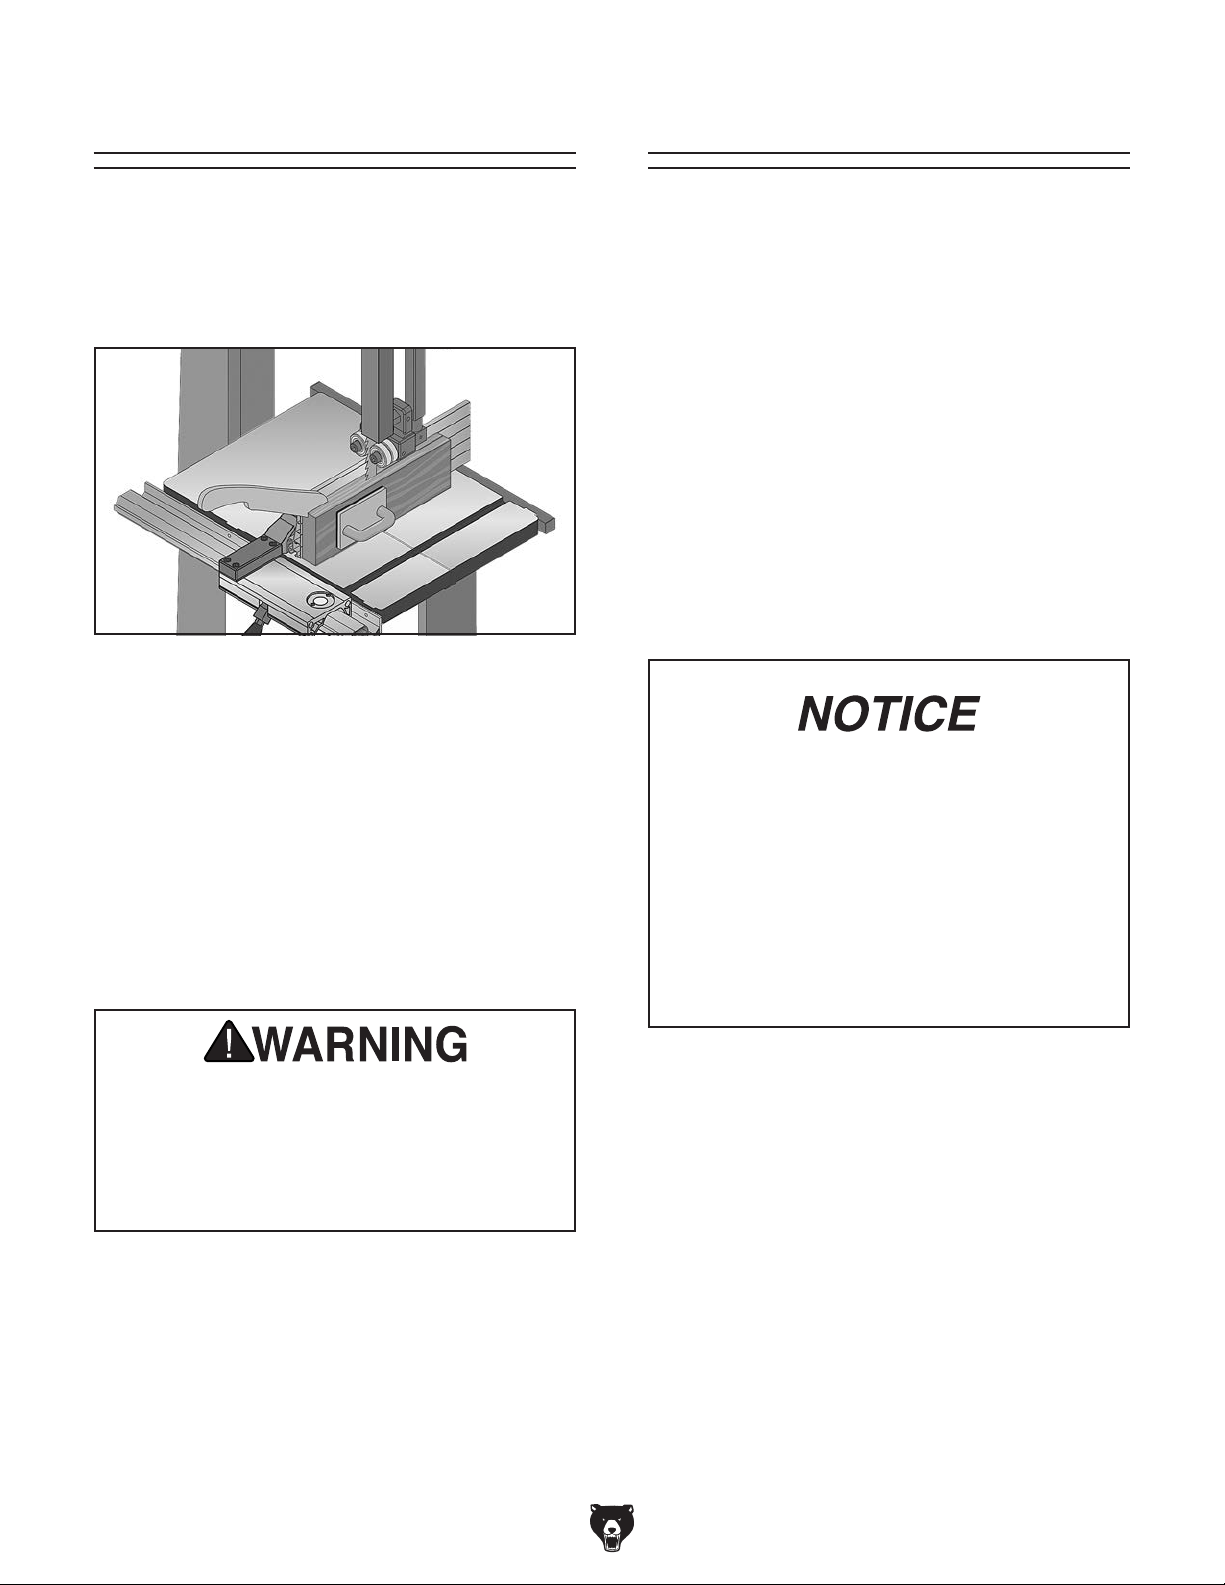
Resawing
Cutting Curves
"Resawing" means cutting the thickness of a
board into two or more thinner boards (see
Figure 54 for an example). The maximum height
of a board that can be resawn is limited by the
maximum cutting height of the bandsaw.
Figure 54. Example of a resawing operation.
One of the most important considerations for
resawing is blade selection—a wide blade cuts
straighter and is less prone to blade lead (see the
Blade Lead subsection later in this manual for
more information).
For most applications, use a blade with a hook or
a skip tooth style. Choose blades with fewer teethper-inch (from 3 to 6 TPI), because they offer larger gullet capacities for clearing sawdust, which
reduces heat buildup and strain on the motor.
When cutting curves, simultaneously feed and
turn the stock carefully so the blade follows the
layout line without twisting. If curves are sharp or
tight, use a narrower blade with more TPI (teeth
per inch) and make relief cuts to avoid having to
back the workpiece away from the blade.
Always make short cuts first, then proceed to
the longer cuts. Relief cuts reduce the chance of
the blade being pinched or twisted. Relief cuts
are cuts made through the waste portion of the
workpiece and are stopped at the layout line, so
when you're cutting along the layout line, waste
wood is released from the workpiece, alleviating
any pressure on the back of the blade. Relief cuts
also make it easier to back the workpiece out once
the saw blade has come to a stop, if needed.
The list below displays blade widths
and the corresponding minimum radii
for those blade widths.
Width Min. Radius
1⁄8" .........................................1⁄8"
3⁄16" .........................................3⁄8"
1⁄4'' .........................................5⁄8''
3⁄8'' ......................................... 11⁄4''
When resawing thin pieces, a wandering
blade (blade lead) can tear through the side
of the workpiece, exposing your hands to
the blade teeth. Always use push blocks
when resawing and keep your hands clear
of the blade.
-42-
Model G0948 (Mfd. Since 08/21)
Page 46
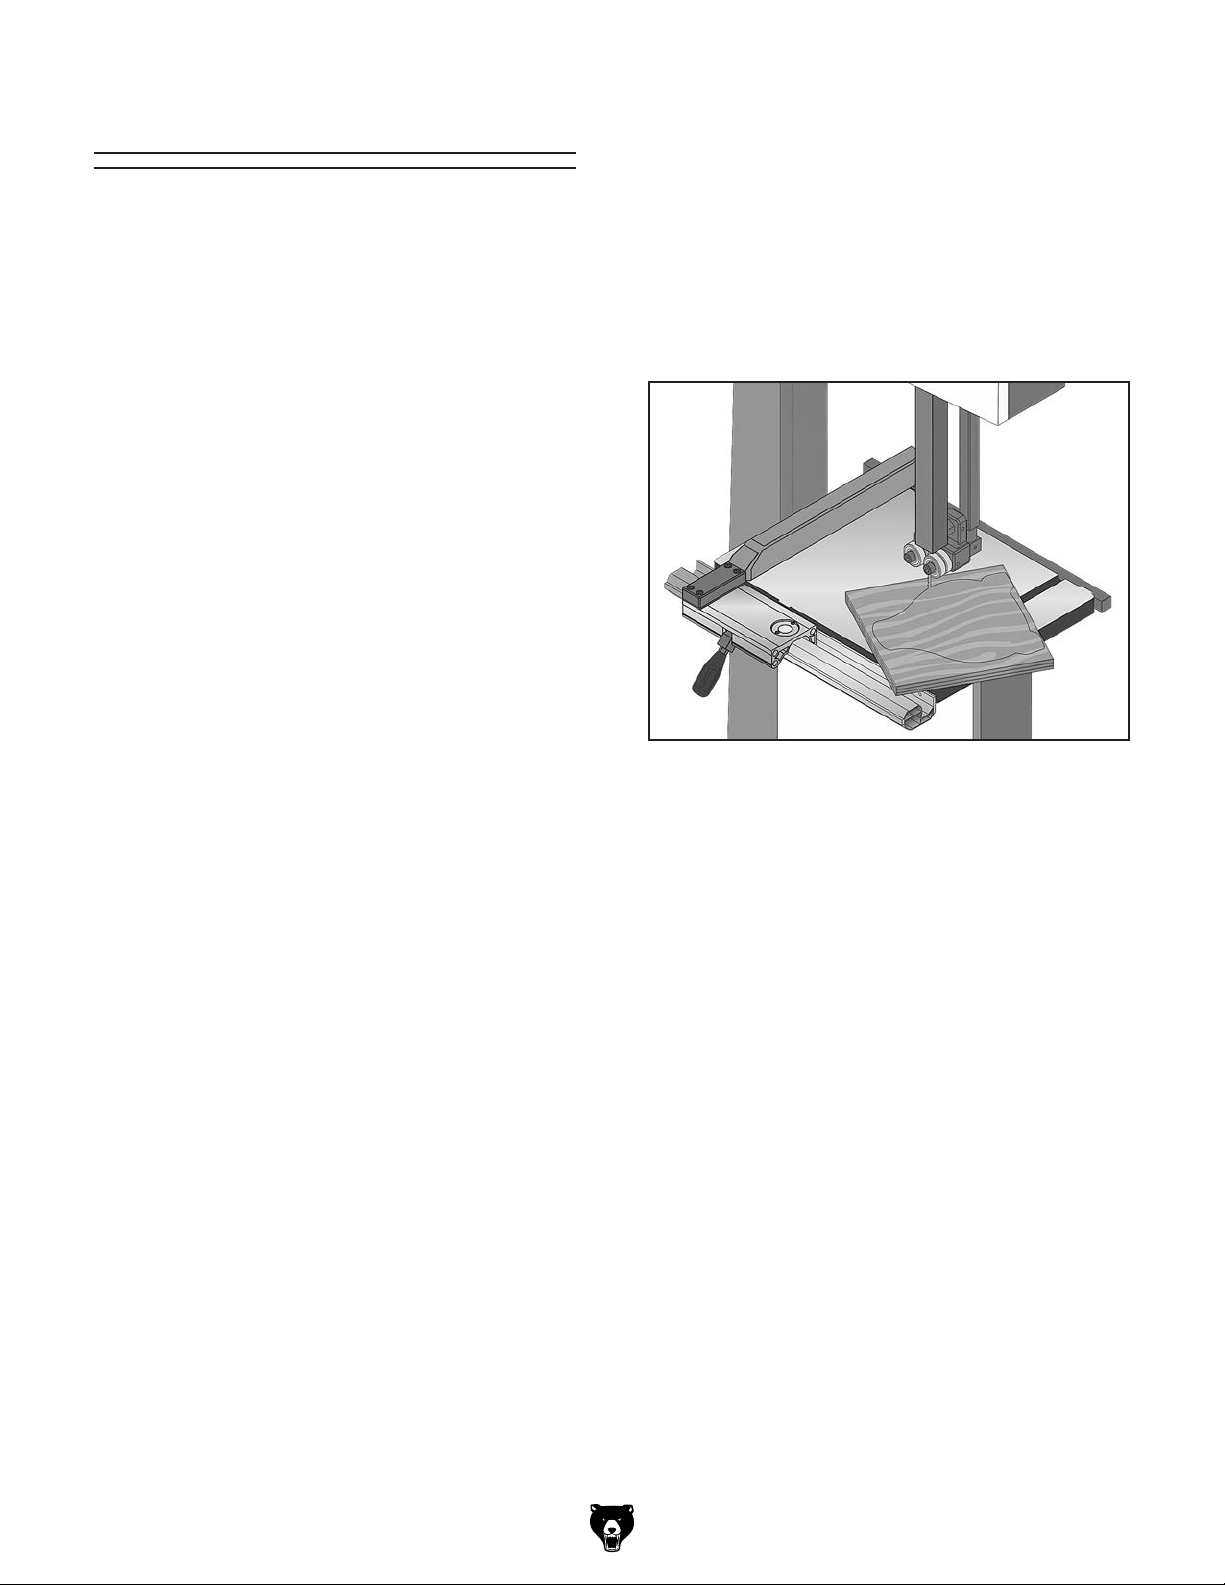
Stacked Cuts
One of the benefits of a bandsaw is its ability to
cut multiple copies of a particular shape by stacking a number of workpieces together. However,
before making stacked cuts, ensure that the table
is perpendicular (90°) to the blade—otherwise,
any error in this setting will be compounded in the
workpieces.
To complete a stacked cut:
Align workpieces from top to bottom.
1.
2. Secure all pieces together in a manner that
will not interfere with cutting. Hot glue on the
edges works well, as do brad nails through
the waste portion. (Be careful not to cut into
the brads or you may break the blade!)
Lay out the shape you intend to cut on face of
3.
top piece.
Make relief cuts perpendicular to outline of
4.
your intended shape in areas where changes
in blade direction could strain woodgrain or
cause blade to bind.
Cut stack of pieces as though you were cut-
5.
ting a single piece. Follow your layout line
with blade kerf on the waste side of your line
(see Figure 55 for an example of a stacked
cut setup).
Figure 55. Example of a stacked cut setup.
Model G0948 (Mfd. Since 08/21)
-43-
Page 47
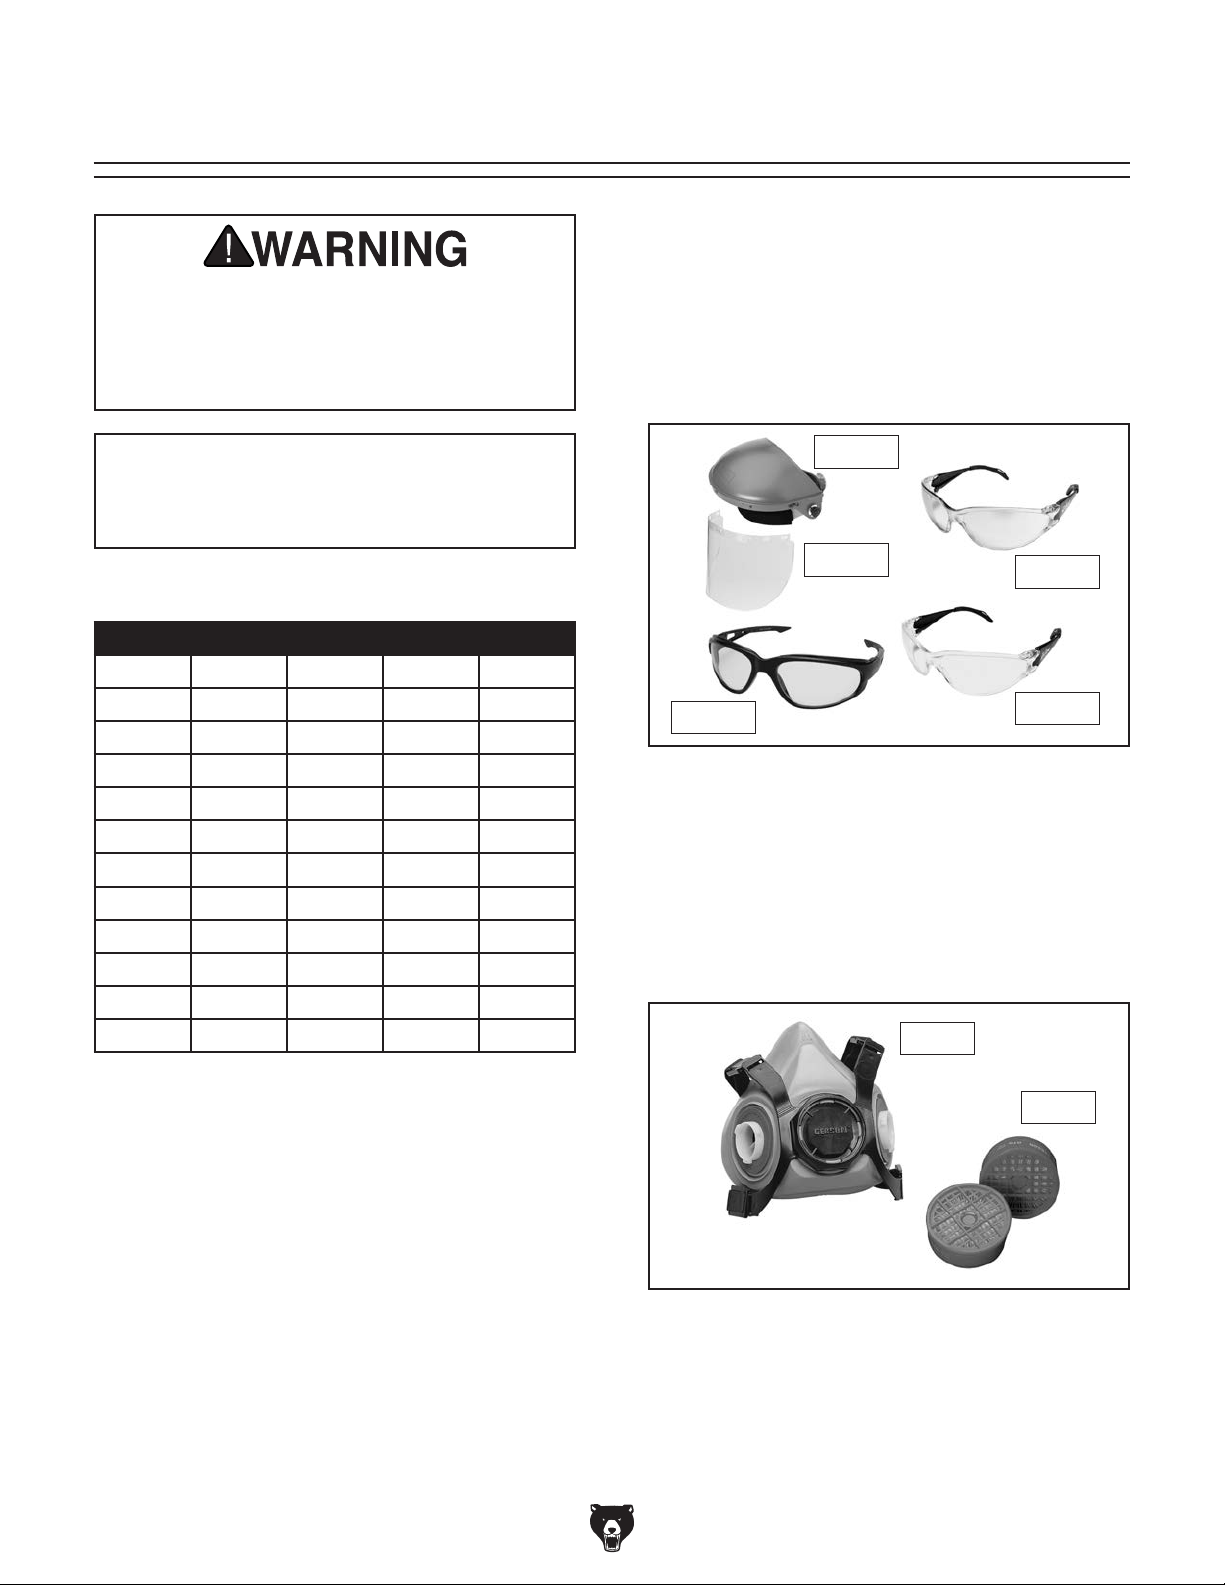
SECTION 5: ACCESSORIES
order online at www.grizzly.com or call 1-800-523-4777
Installing unapproved accessories may
cause machine to malfunction, resulting in
serious personal injury or machine damage.
To reduce this risk, only install accessories
recommended for this machine by Grizzly.
NOTICE
Refer to our website or latest catalog for
additional recommended accessories.
Grizzly 72" Bandsaw Blades
Model Width TPI Type Gauge
T33130
T33131
T33132
T33133
T33134
T33135
T33136
T33137
T33138
T33139
T3 3140
T33141
1
⁄8" 14 Raker 0.025
3
⁄16" 4 Skip 0.025
3
⁄16" 14 Raker 0.025
1
⁄4" 4 Hook 0.025
1
⁄4" 6 Hook 0.025
1
⁄4" 10 Raker 0.025
3
⁄8" 4 Hook 0.025
3
⁄8" 6 Hook 0.025
3
⁄8" 10 Raker 0.025
3
⁄8" 14 Raker 0.025
1
⁄2 " 3 Hook 0.025
1
⁄2 " 4 Hook 0.025
Basic Eye Protection
T20501—Face Shield Crown Protector 4"
T20502—Face Shield Crown Protector 7"
T20503—Face Shield Window
T20451—“Kirova” Clear Safety Glasses
T20452—“Kirova” Anti-Reflective S. Glasses
T20456—DAKURA Safety Glasses
T20502
T20503
T20456
Figure 56. Assortment of basic eye protection.
H2499—Small Half-Mask Respirator
H3631—Medium Half-Mask Respirator
H3632—Large Half-Mask Respirator
H3635—Cartridge Filter Pair P100
If you work around dust everyday, a half-mask
respirator can be a lifesaver. Also compatible with
safety glasses!
H3631
T20452
T20451
Figure 57. Half-mask respirator with disposable
cartridge filters.
-44-
Model G0948 (Mfd. Since 08/21)
H3635
Page 48
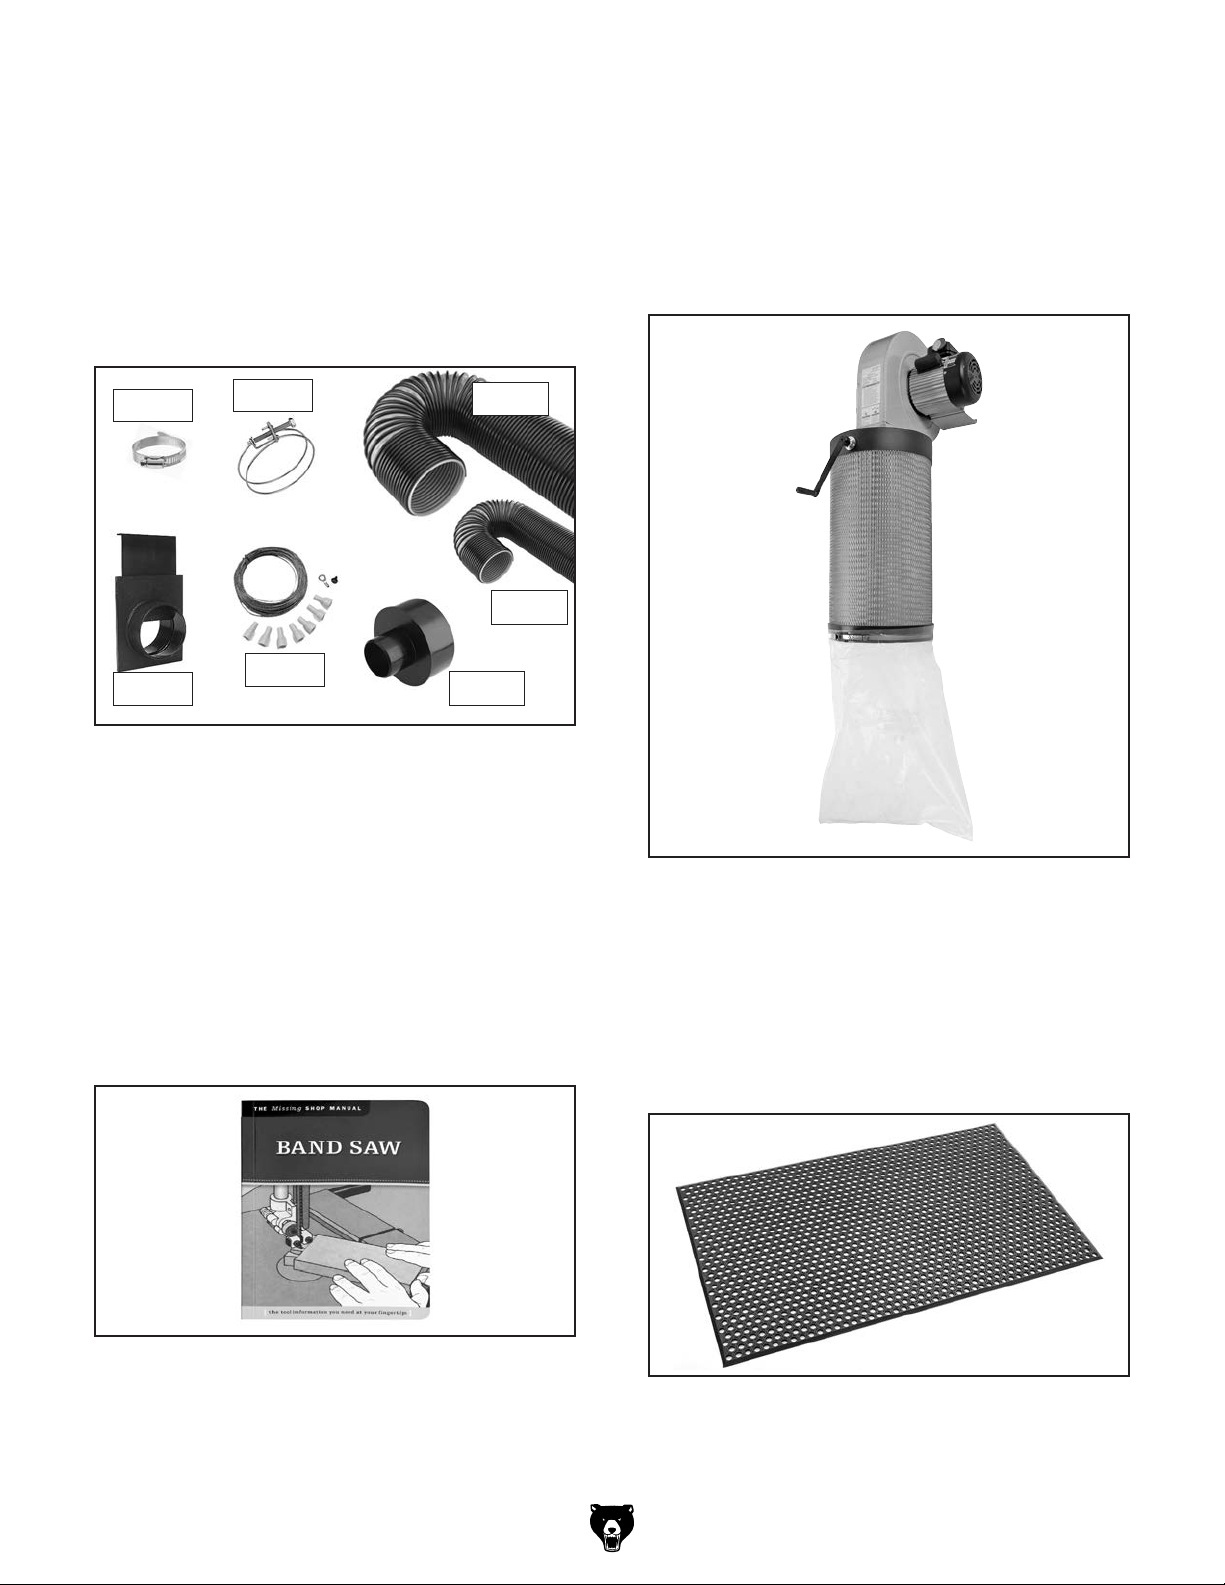
order online at www.grizzly.com or call 1-800-523-4777
W1025—Hose Clamp 2 "
W1317—Wire Hose Clamp 4"
D4226—Dust Collection Reducer 2 " x 4" OD
D4206—4" x 10' Clear Hose
D4202—2" x 10' Clear Hose
W1007—Plastic Blast Gate 4"
W1053—Anti-Static Grounding Kit
We've hand picked a selection of dust collection
components commonly needed to connect your
new machine to basic dust collection.
G0944—1 1⁄2 HP Wall-Mount Dust Collector
With an airflow capacity of 1250 CFM and a canister filter with a 1-micron filtration rating, this is
the beast you need for all your small shop dustcapturing needs. The easy-to-hang French cleatstyle mount makes hanging this unit quick, and
clears up your floor space allowing for more room
in a small shop.
W1025
W1317
D4206
D4202
W1053
W1007
D4226
Figure 58. Dust collection accessories.
T26403—The Missing Shop Manual: Bandsaw
Dedicated to providing integral information about
woodworking tools and techniques that other
manuals overlook, the books in this series contain
safety facts, explanations about basic project set
up, and tips for maximizing tool performance. In
Bandsaw, you will learn how to best utilize this
essential workshop tool. Filled with clear diagrams
and instructions, this pocket sized durable manual
is ideal for quick reference in the workshop. 112
pages, soft cover.
Figure 60. G0944 1 1⁄2 HP Wall-Mount Dust
Collector with Canister Filter.
T10456—Heavy-Duty Anti-Fatigue Mat 3' x 5'
This Heavy-Duty Anti-Fatigue Mat features beveled edges and no-slip tread for safety and
comfort. Open-hole design allows liquid to drain
through, so it's perfect for wet or oily conditions.
3
Measures 3' wide x 5' long x
⁄8" thick.
Figure 59. The Missing Shop Manual: Bandsaw.
Figure 61. T10456 Anti-Fatigue Mat.
Model G0948 (Mfd. Since 08/21)
-45-
Page 49
order online at www.grizzly.com or call 1-800-523-4777
T21580—36" Bevel Edge Straight Edge
These 36" Bevel Edge Straight Edges are made
from hardened steel with satin chrome finish and
are precision ground and lapped for straightness
and parallelism.
Figure 62. T21580 Bevel Edge Straight Edge.
H7978—6" Fractional Digital Caliper
Large LCD readout converts to decimal inch,
fractional inch, and millimeters with the push of
a button. Measure internal, external dimensions,
depth, steps, and differential measurements.
Features thumb roll and stainless steel construction. Range: 0-6", 0-150mm. Resolution: 0.0005",
1
0.01mm,
⁄128".
T32407—Grip Snap-Ring Pliers Set, 10 -Pc.
This plier set allows you to operate both internal
and external rings. Includes 4 bent and 4 straight
pliers made of heat-treated steel in sizes 5
1⁄2 " to
9". The 5" and 6" pliers have a 1.2mm (.047") tip;
7 1⁄2" and 8" pliers have a 1.8mm (.07") tip;
the
and the
8 1⁄2 " and 9" pliers have a 2.3mm (0.9") tip.
The set includes one 5" hook, one 5" pick, and an
impact-resistant carrying case.
Figure 64. T32407 Grip Snap-Ring Plier Set.
Figure 63. H7978 6" Fractional Digital Caliper.
-46-
Model G0948 (Mfd. Since 08/21)
Page 50
SECTION 6: MAINTENANCE
To reduce risk of shock or
accidental startup, always
disconnect machine from
power before adjustments,
maintenance, or service.
Schedule
For optimum performance from this machine, this
maintenance schedule must be strictly followed.
Ongoing
To minimize your risk of injury and maintain proper
machine operation, shut down the machine immediately if you ever observe any of the items below,
and fix the problem before continuing operations:
Cleaning &
Lubricating
Vacuum excess wood chips and sawdust, and
wipe off the remaining dust with a dry cloth. If
resin has built up, use a resin dissolving cleaner
to remove it.
Once a month, remove the blade and thoroughly
clean all built-up sawdust from the rubber tires on
the wheels.
If the table becomes difficult to tilt, lubricate the
surfaces between the trunnions and the trunnion
bracket with a dry lubricant (see Figure 65).
• Loose mounting bolts.
• Damaged saw blade.
Worn or damaged wires.
•
Any other unsafe condition.
•
Monthly
• Check belt for tension, damage, or wear.
• Remove blade and thoroughly clean all built-
up sawdust from the rubber tires on the
wheels.
• Clean/vacuum dust buildup from inside cabi-
net and off motor.
Figure 65. Model G4682 Dry Coating Lube.
Model G0948 (Mfd. Since 08/21)
-47-
Page 51
Review the troubleshooting procedures in this section if a problem develops with your machine. If you need
the
serial number and manufacture date of your machine before calling.
SECTION 7: SERVICE
replacement parts or additional help with a procedure, call our Technical Support. Note: Please gather
Troubleshooting
Motor & Electrical
Symptom Possible Cause Possible Solution
Machine does not
start, or power
supply breaker
immediately trips
after startup.
Machine stalls or
is underpowered.
1. Switch disabling key removed.
2. Incorrect power supply voltage or circuit size.
3. Power supply circuit breaker tripped or fuse
blown.
4. Start capacitor at fault.
5. Centrifugal switch adjustment/contact point at
fault.
6. Wiring broken, disconnected, or corroded.
7. ON/OFF switch at fault.
8. Motor or motor bearings at fault.
1. Dull blade.
2. Workpiece material unsuitable for machine.
3. Feed rate/cutting speed too fast.
4. Workpiece crooked; fence loose or
misadjusted.
5. Dust collection ducting problem.
6. Machine undersized for task.
7. Blade slipping on wheels or not properly
tensioned.
8. Belt(s) slipping/pulleys misaligned.
9. Motor wired incorrectly.
10. Pulley slipping on shaft.
11. Motor overheated.
12. Extension cord too long.
13. Centrifugal switch/contact points at fault.
14 Motor or motor bearings at fault.
1. Install switch disabling key.
2. Ensure correct power supply voltage and circuit size
(Page 11).
3. Ensure circuit is sized correctly and free of shorts.
Reset circuit breaker or replace fuse.
4. Test/replace if at fault.
5. Adjust centrifugal switch/clean contact points.
Replace either if at fault.
6. Fix broken wires or disconnected/corroded
connections.
7. Replace switch.
8. Replace motor.
1. Sharpen/replace blade (Page 39).
2. Only cut wood/ensure moisture is below 20%.
3. Decrease feed rate/cutting speed.
4. Straighten or replace workpiece/adjust fence.
5. Clear blockages, seal leaks, use smooth wall duct,
elminate bends, close other branches.
6. Use correct blade/reduce feed rate or depth of cut.
7. Adjust blade tracking and tension (Pages 20–22).
8. Clean/tension/replace belt(s) (Page 52); ensure
pulleys are aligned (Page 53).
9. Wire motor correctly (Page 59).
10. Tighten/replace loose pulley/shaft.
11. Clean motor, let cool, and reduce workload.
12. Move machine closer to power supply; use shorter
extension cord (Page 12).
13. Adjust centrifugal switch/clean contact points.
Replace either if at fault.
14. Replace motor.
-48-
Model G0948 (Mfd. Since 08/21)
Page 52
Symptom Possible Cause Possible Solution
Machine has
vibration or noisy
operation.
Blade or teeth
break/crack.
1. Motor or component loose.
2. Blade weld at fault/teeth broken.
3. Blade at fault.
4. V-belt worn, loose, pulleys misaligned or belt
slapping cover.
5. Pulley loose.
6. Motor mount loose/broken.
7. Motor fan rubbing on fan cover.
8. Centrifugal switch.
9. Motor bearings at fault.
1. Blade tension incorrect.
2. Blade incorrect for application.
3. Excessive feed rate/pressure.
4. Cutting corners too sharply.
5. Blade dull/weld at fault.
6. Blade is tracking incorrectly.
7. Blade guides/support bearings not adjusted
properly, allowing guides to hit blade teeth.
8. Wheel tires worn or incorrectly installed.
9. Fence or miter slot out of alignment with
blade.
10. Bad bearings on wheels or guide bearings.
1. Replace damaged or missing bolts/nuts or tighten if
loose.
2. Replace blade (Page 39).
3. Replace warped/bent blade (Page 39); resharpen
dull blade.
4. Inspect/replace belt with a new matched set (Page
52). Re-align pulleys if necessary (Page 53).
5. Secure pulley on shaft.
6. Tighten/replace.
7. Fix/replace fan cover; replace loose/damaged fan.
8. Replace switch.
9. Test by rotating shaft; rotational grinding/loose shaft
requires bearing replacement.
1. Adjust blade tension (Page 22).
2. Use correct blade for application (Page 37).
3. Reduce feed rate/pressure.
4. Use a wider arc on outside cuts, or use relief cuts to
make tight inside cuts.
5. Replace blade (Page 39).
6. Adjust blade tracking (Page 20).
7. Adjust blade guide bearings properly so guides
cannot contact teeth during operation (Pages
24–25).
8. Replace or re-install tire.
9. Align table miter slot and fence with blade (Pages
27–28).
10. Replace wheels and/or guide bearings.
Blade slows,
smokes, shows
overheating or
wears on one
side.
Finished
workpieces are
rough or show
scoring.
Gullets loaded
with chips.
1. Blade contacting table insert.
2. Blade guides worn or misadjusted.
3. Blade installed backwards.
4. Too much side pressure when feeding
workpiece.
5. Wheels are out of alignment.
6. Dull, bell-mouted, or incorrect blade.
7. Fence not parallel with blade.
8. Table top surface is not parallel or square to
blade.
9. V-belt loose or slipping.
1. Blade is overloaded and twists.
2. Blade TPI too coarse.
3. Blade is loose and fluttering.
4. Blade tracking is incorrect.
5. Blade has missing/bent teeth or faulty weld.
1. Excessive feed rate/pressure.
2. Blade TPI is too fine.
1. Adjust blade guide bearings to eliminate excess
side pressure (Pages 24–25); properly align table
(Page 27).
2. Adjust blade guide bracket.
3. Check blade rotation. Re-install blade if necessary
(Page 39).
4. Feed workpiece straight into blade.
5. Adjust wheels to be coplanar (Page 53).
6. Replace blade (Page 39).
7. Adjust fence parallel with blade (Page 28).
8. Adjust/shim table/trunnion position until blade and
table are parallel and square (Page 27)
9. Tighten V-belt. Replace if worn or oily (Page 51).
1. Decrease feed rate; ensure proper TPI (Page 34).
2. Use correct blade for material and speed of cut
(Page 37).
3. Adjust blade tension as required (Page 22).
4. Adjust blade tracking (Page 20).
5. Replace blade (Page 39).
1. Reduce feed rate/pressure.
2. Install correct blade (Page 34).
Model G0948 (Mfd. Since 08/21)
-49-
Page 53
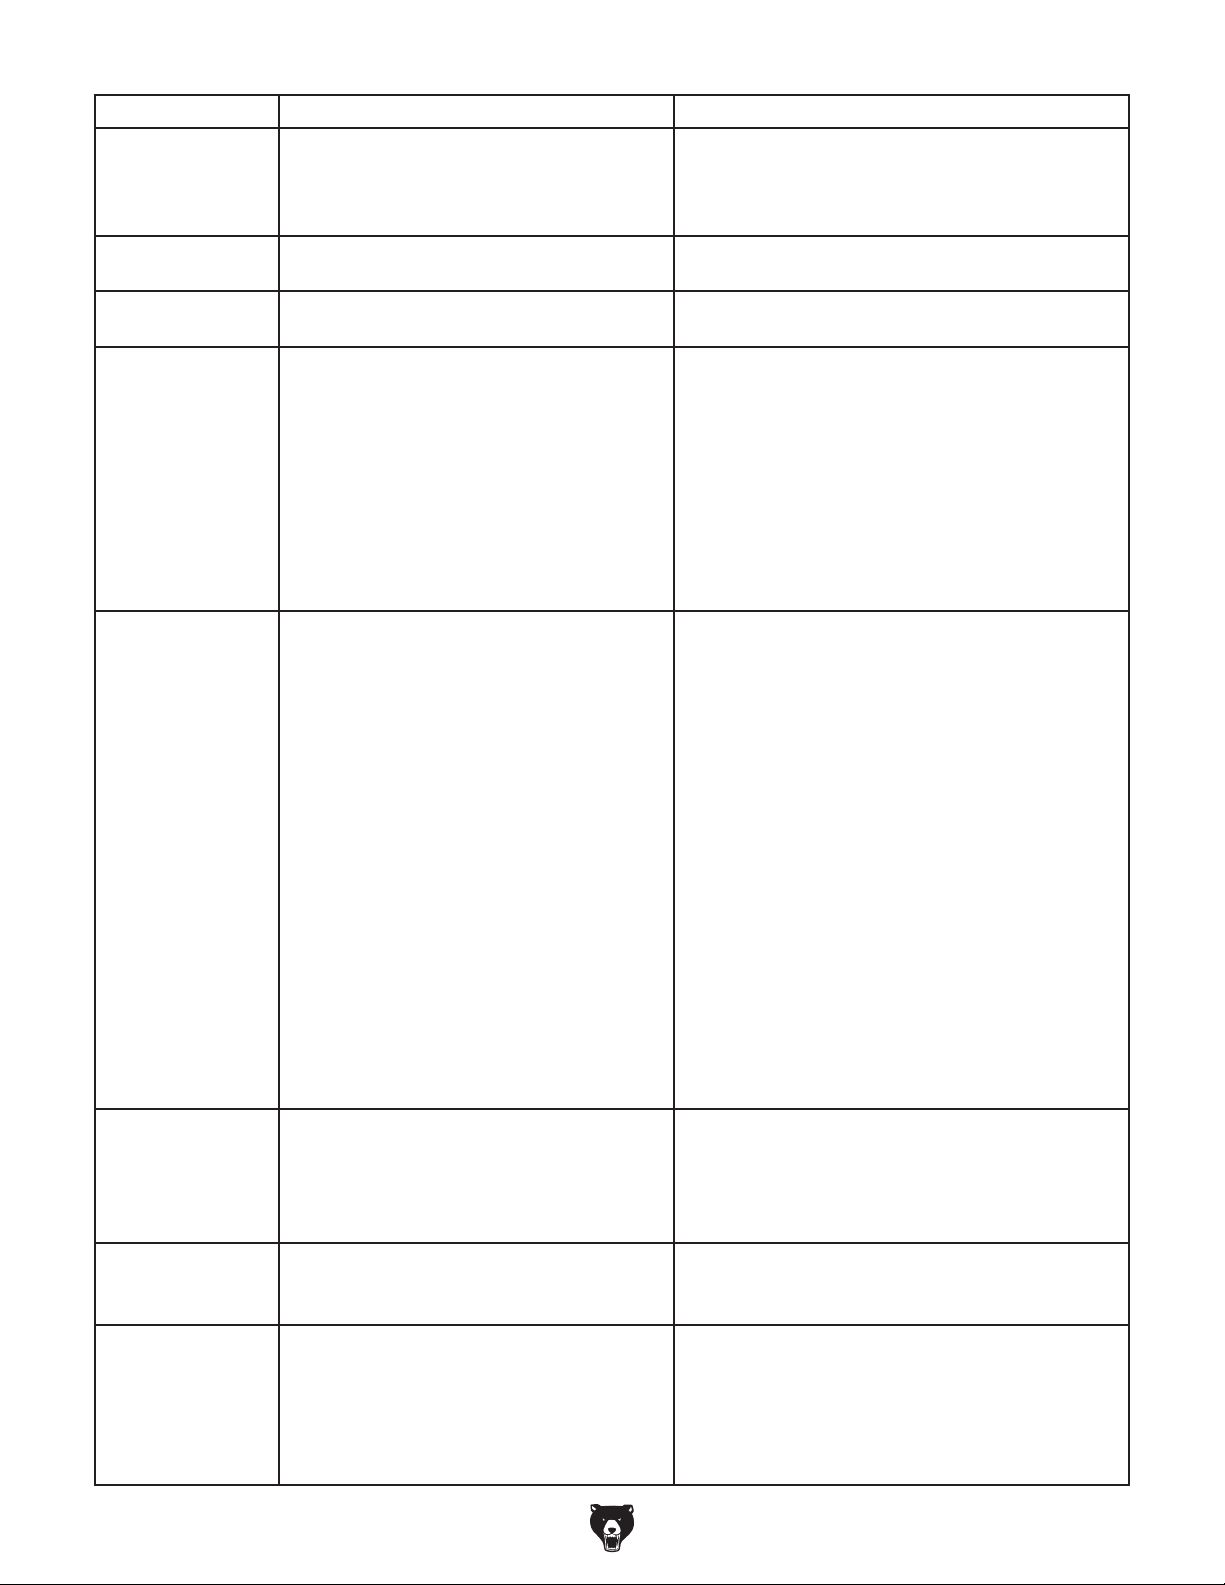
Symptom Possible Cause Possible Solution
Table is hard to tilt. 1. Table tilt lock lever is engaged.
2. Sawdust or pitch trapped between trunnion
and base.
3. Metal burrs on trunnion.
Table does not tilt to
45 or 0 degrees.
Miter bar binds in
miter slot.
Blade tracks
incorrectly or comes
off wheels.
Cut is crooked or
blade wanders
(blade lead).
Blade dulls
prematurely.
Backside of blade
deformed/cracked.
Sawdust buildup
inside cabinet.
1. Table tilt scale indicator not calibrated.
2. Positive stop not set correctly.
1. Miter slot dirty or gummed up.
2. Miter bar bent.
1. Tracking is not adjusted properly.
2. Wheels are not coplanar.
3. Blade tension too loose.
4. Blade guides/support bearings improperly
adjusted.
5. Feeding workpiece too fast.
6. Incorrect blade for operation.
7. Blade is bell-mouthed, worn, or dull.
8. Wheel is damaged or worn.
1. Excessive feed rate/pressure.
2. Blade tension too loose.
3. Blade is too narrow or tooth type/TPI is
incorrect for the cut.
4. Inadequate blade support.
5. Blade dull or has damaged tooth set from
improper blade guide/support bearing
adjustment.
6. Blade tracking is incorrect.
7. Table is loose.
8. Fence or miter slot out of alignment with
blade.
9. Blade guides/support bearings improperly
adjusted.
10. Tooth set is uneven or teeth are sharper on
one side than the other.
1. Excessive feed rate/pressure.
2. Wrong blade tooth type or TPI.
3. Blade is twisted.
4. Blade is slipping on wheel.
5. Blade guides hitting teeth, ruining tooth set.
1. Excessive feed rate/pressure.
2. Blade tension too high.
3. Blade support bearings improperly adjusted.
1. Blade brush worn or misadjusted.
2. Clogged dust port.
3. Low CFM (airflow) from dust collection
system.
1. Disengage table tilt lock lever (Page 32).
2. Remove table and clean trunnion sliding surfaces
free of sawdust or pitch.
3. Remove burrs.
1. Calibrate table tilt scale indicator (Page 33).
2. Adjust positive stop (Page 33).
1. Carefully clean miter slot.
2. Replace.
1. Adjust tracking (Page 20).
2. Adjust wheels to be coplanar (Page 53).
3. Increase blade tension (Page 22).
4. Properly adjust blade guides/support bearings
(Pages 24–25).
5. Feed workpiece slower.
6. Install correct blade (Page 37).
7. Install new blade (Page 39), and remove tension
from blade when not in use.
8. Replace wheel.
1. Reduce feed rate/pressure.
2. Increase blade tension (Page 22).
3. Use wider blade. Ensure tooth type and TPI are
correct (Page 34).
4. Position upper blade guides to just clear workpiece.
Properly adjust blade guides/support bearings
(Pages 24–25).
5. Replace blade (Page 39).
6. Adjust blade tracking (Page 20).
7. Tighten table trunnion mounting bolts or tilt lock
lever.
8. Align miter slot and fence with blade (Pages
27–28).
9. Properly adjust blade guides/support bearings
(Pages 24–25).
10. Replace blade (Page 39).
1. Reduce feed rate/pressure.
2. Use blade with correct tooth type and TPI (Page 34).
3. Re-install blade; replace (Page 39).
4. Adjust blade tension (Page 34).
5. Properly adjust guide bearings (Pages 24–25).
1. Reduce feed rate/pressure.
2. Adjust blade tension (Page 34).
3. Properly adjust blade support bearings (Page 24).
1. Properly adjust brush; replace if necessary
(Page 57).
2. Clean dust port.
3. Inspect ducting for leaks/clogs and repair as
necessary; move dust collector closer to machine;
install a stronger dust collector (Page 19).
-50-
Model G0948 (Mfd. Since 08/21)
Page 54
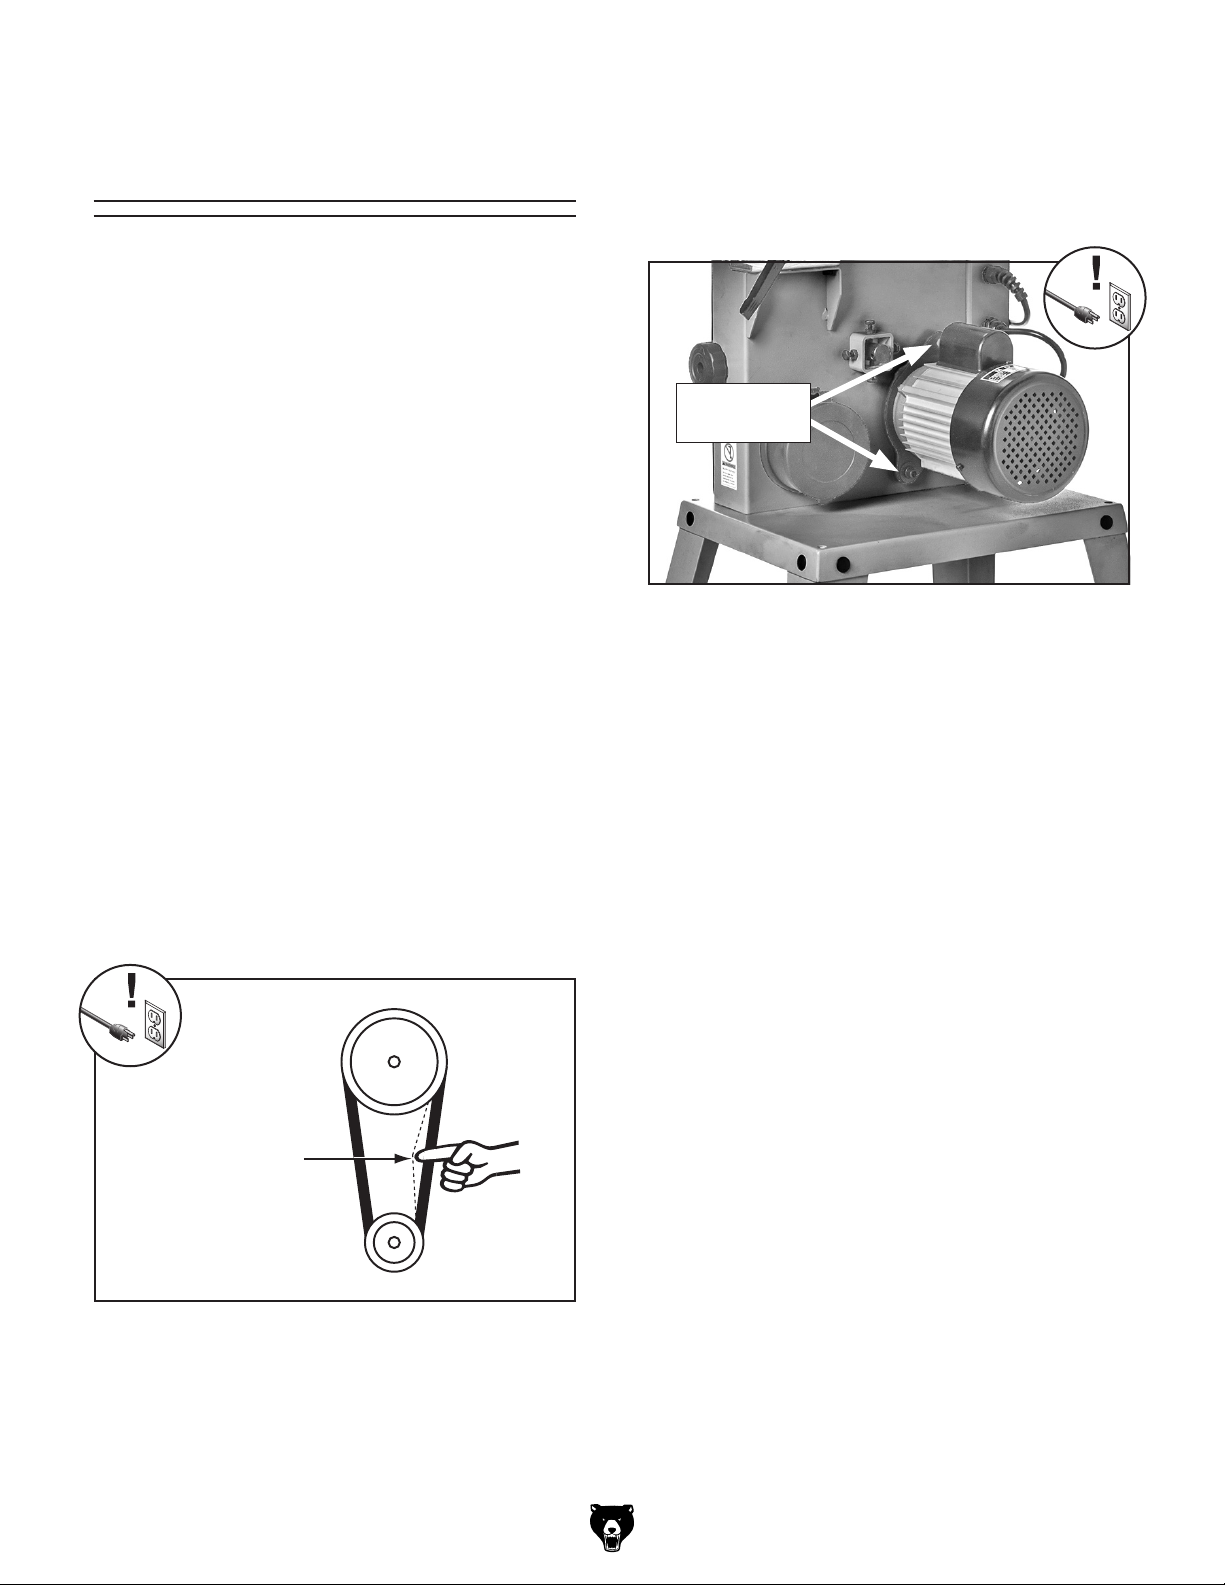
Checking/Adjusting
Belt Tension
To ensure optimum power transmission from the
motor to the blade, the belt must be in good condition and operate under proper tension.
Belt tension should be checked at least every
month—more often if the bandsaw is used daily. If
the belt shows signs of cracks, fraying, and excessive wear, replace it as instructed in Replacing
Belt on Page 52.
Item(s) Needed Qty
Hex Wrench 6mm .............................................. 1
Adjusting Belt Tension
DISCONNECT MACHINE FROM POWER!
1.
Loosen motor mount cap screws shown in
2.
Figure
Motor Mount
Cap Screws
67.
Checking Belt Tension
1. DISCONNECT MACHINE FROM POWER!
Open lower wheel cover.
2.
3. Check belt condition and deflection. The belt
is properly tensioned if there is approximately
3
⁄8" deflection. Deflection is checked by push-
ing belt with moderate pressure, as shown in
Figure 66, and noting how much it moves.
— If belt is not properly tensioned, per-
form Adjusting Belt Tension
procedure.
Wheel Pulley
Approximately
3
/8" Deflection
Figure 67. Location of motor mount cap screws
used for adjusting belt tension.
3. Push motor to the right (as viewed from back
of machine) until you feel moderate tension,
then tighten both cap screws.
Check belt tension. If necessary, repeat
4.
Steps 2–3 until there is approximately 3⁄8"
deflection in belt.
Close wheel cover.
5.
Motor Pulley
Figure 66. Checking belt tension.
Model G0948 (Mfd. Since 08/21)
-51-
Page 55
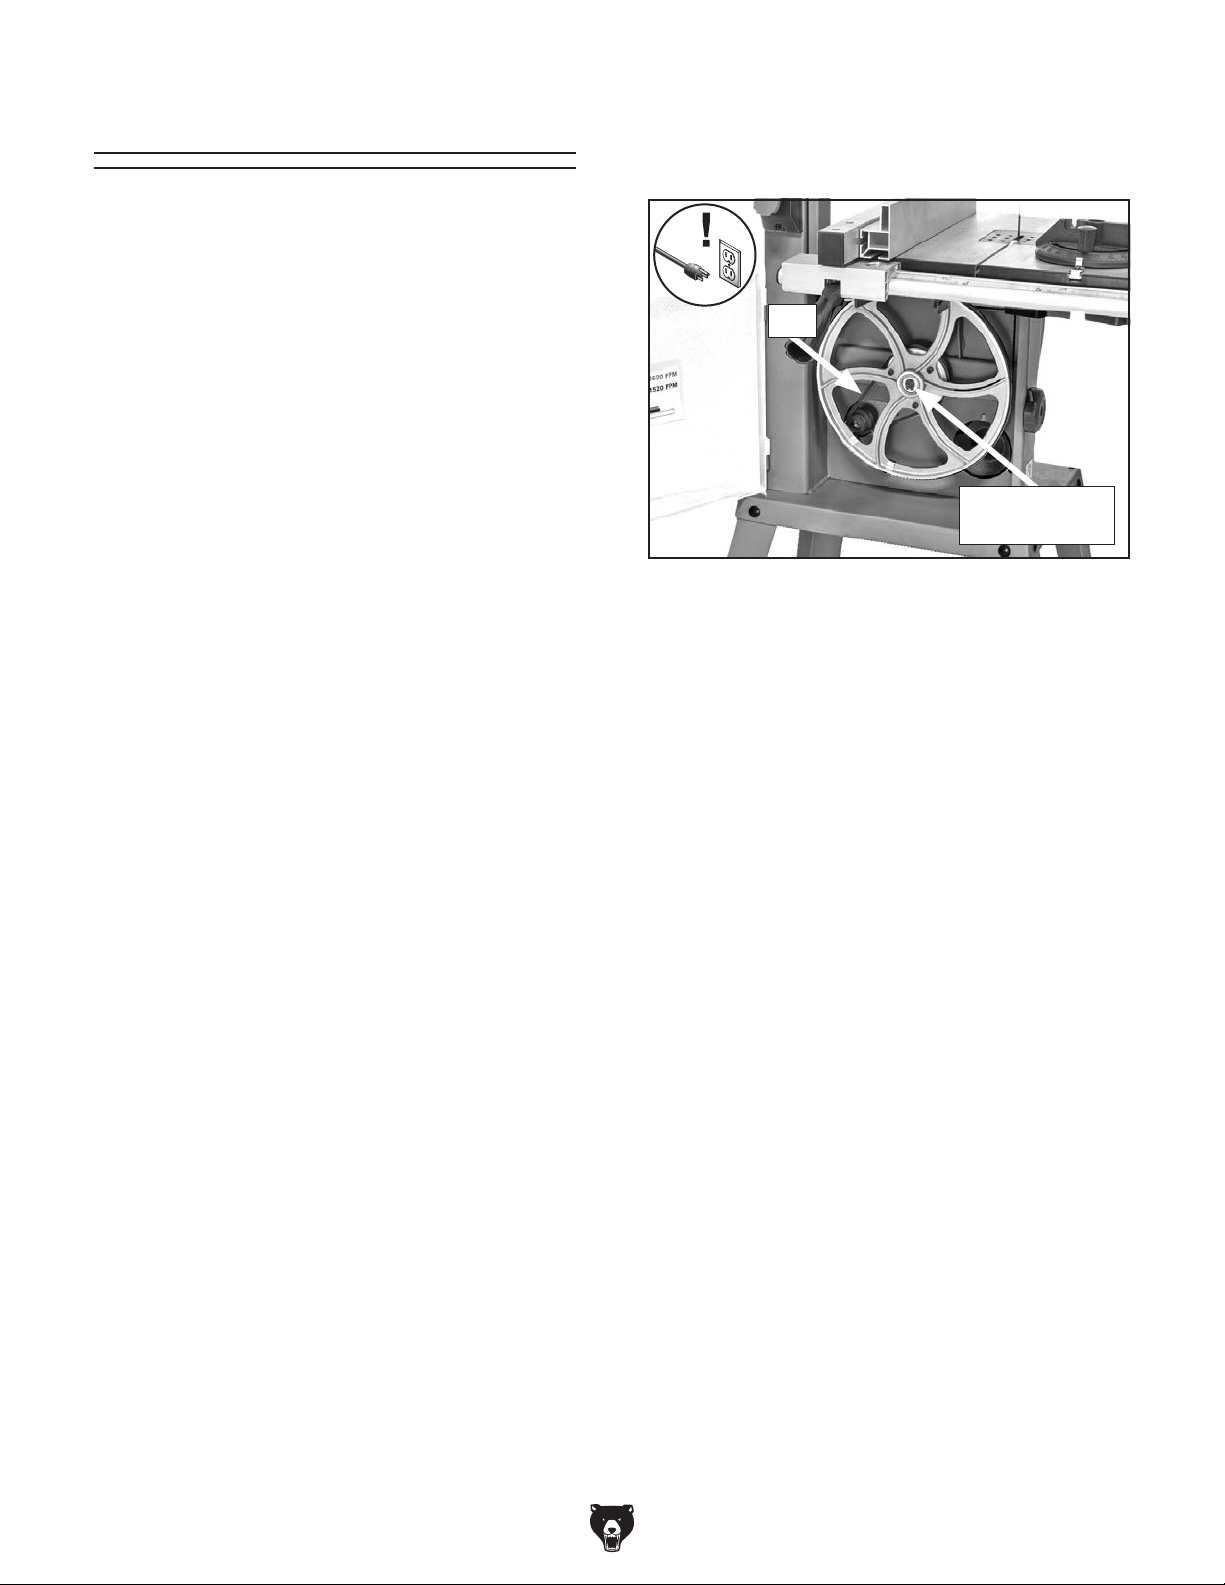
Replacing Belt
To ensure optimum power transmission from the
motor to the blade, the belt must be in good condition and be properly tensioned.
Remove external retaining ring from lower
6.
wheel shaft (see
lower wheel.
Figure 68) and remove
Replace the belt if it shows signs of cracking, fraying, or excessive wear.
Item(s) Needed Qty
Hex Wrench 6mm .............................................. 1
Retaining Ring Pliers
Heavy Leather Gloves
Replacement Belt (Part # P0948105)
To replace belt:
DISCONNECT MACHINE FROM POWER!
1.
Put on heavy leather gloves and remove
2.
blade from machine (refer to Removing/
Installing Blade on
Loosen motor mount cap screws (see
3.
Figure
Pivot motor to the right (as viewed from back
4.
of bandsaw) to release belt tension.
Open lower wheel cover and remove belt
5.
from motor pulley.
67 on Page 51).
......................................... 1
..................................1 Pr.
................ 1
Page 39).
Belt
External
Retaining Ring
Figure 68. Belt change components inside lower
wheel compartment.
Install new belt on both pulleys, and then re-
7.
install wheel and retaining ring.
Properly tension belt, as instructed in
8.
Adjusting Belt Tension on Page
Install blade, properly track and tension blade
9.
(see Pages 20 & 22), and adjust support
bearings and guide bearings (see Pages
24–25).
51.
-52-
Model G0948 (Mfd. Since 08/21)
Page 56
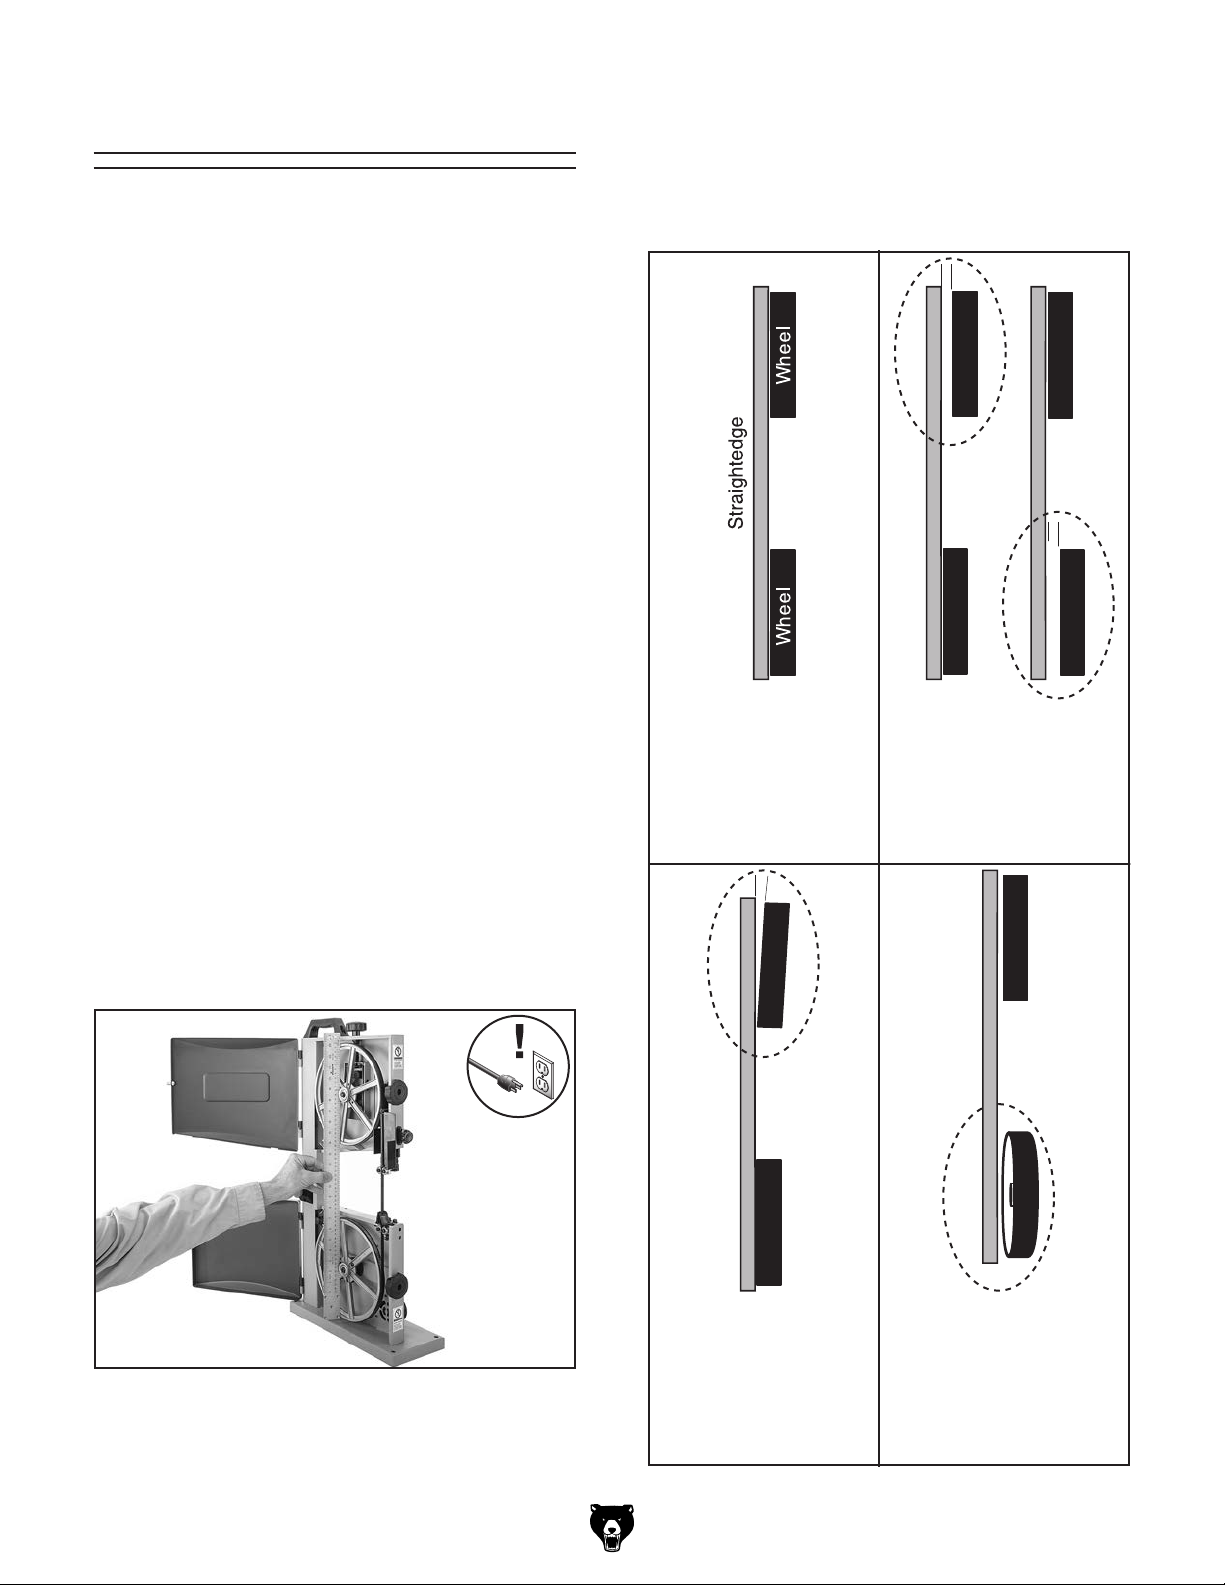
aligning wheels
Aligning Wheels
Wheel alignment is important for optimal performance from your bandsaw. Wheels are properly
aligned when they are parallel with each other and
in the same plane or “coplanar” (see the illustration in the figure to the right).
When wheels are coplanar, the bandsaw is
more likely to cut straight without wandering; and
vibration, heat, and blade wear are considerably
decreased because the blade is automatically balanced on the wheel.
Bringing the wheels into alignment may require a
combination of shimming a wheel and adjusting
the position of the lower wheel shaft.
Checking Wheel Alignment
Tool(s) Needed Qty
Precision Straightedge 3'. .................................. 1
Check wheel alignment, and adjust tracking
4.
knob to bring both wheels into alignment as
much as possible. If wheels cannot be adjusted coplanar, use Figure 70 to determine how
to proceed with alignment adjustments.
or
To check wheel alignment:
DISCONNECT MACHINE FROM POWER!
1.
Remove table.
2.
3. With blade on and properly tensioned, hold a
straightedge close to center of both wheels.
Make sure straightedge fully extends across
rims of both wheels, as shown in Figure 69.
Wheels parallel and
aligned: No adjust-
ment needed.
Wheels parallel, but
upper or lower wheel
is not coplanar with the
other wheel: Move the
upper wheel in or out.
Figure 69. Example of checking if wheels are
coplanar.
Model G0948 (Mfd. Since 08/21)
Upper wheel is not
vertically aligned with
lower wheel: Use
blade tracking knob
to tilt upper wheel.
Figure 70. Wheel alignment illustration.
Lower wheel is not
laterally aligned with
upper wheel: Adjust
rear adjustment set
bolts to tilt lower wheel
left/right.
-53-
Page 57
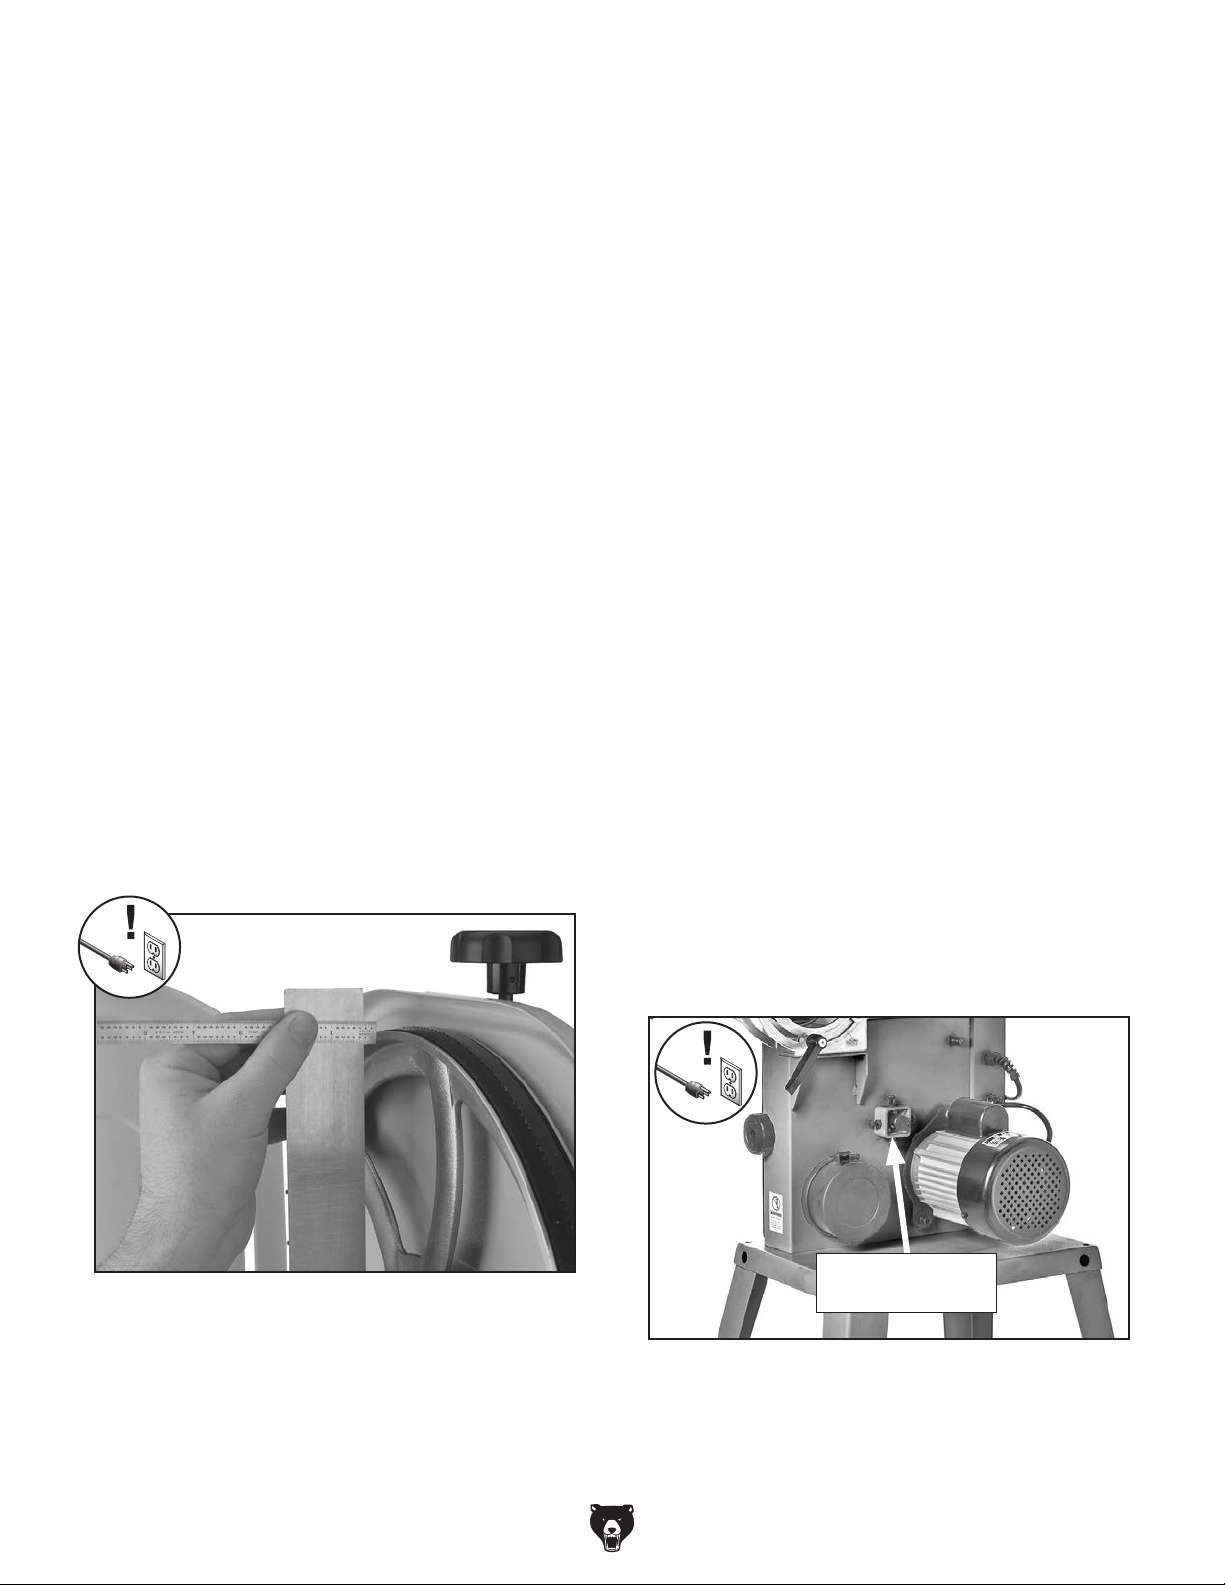
Shimming a Wheel
A wheel that is parallel with the other wheel, but
is not coplanar, must be shimmed by the distance
that it is not in the same plane with the other
wheel.
Tip: Standard washers work well for shimming the
wheel because they can easily be stacked to get
the desired height.
Item(s) Needed Qty
Precision Straightedge 3'. .................................. 1
Fine Ruler
Retaining Ring Pliers
Heavy Leather Gloves
Shims
.......................................................... 1
......................................... 1
..................................1 Pr.
................................................. As Needed
6. Re-install wheel and secure it in place.
7. Re-install blade and properly tension it.
Perform previous Checking Wheel
8.
Alignment procedure. If necessary to make
the wheels parallel, repeat this procedure.
The first time you get the wheels coplanar,
9.
place a mark on each wheel where you held
the straightedge, then use this position again
in the future if you need to repeat the procedure. This assures repeated accuracy every
time you adjust the wheels.
Close wheel covers.
10.
To shim a wheel:
DISCONNECT MACHINE FROM POWER!
1.
Adjust upper wheel tracking so that it is paral-
2.
lel with lower wheel.
With straightedge touching both rims of wheel
3.
that does not need to be adjusted, measure
the distance away from the other wheel with
a fine ruler, as shown in Figure 71. The distance measured with the ruler is the distance
this wheel must be shimmed.
Adjusting Lower Wheel Shaft Position
If the lower wheel is tilted laterally (side to side),
perform the following procedure to make it coplanar with the upper wheel.
There are four adjustment bolts with hex nuts in
the lower wheel bracket, shown in Figure 72, that
adjust the wheel tilt from side-to-side and up-anddown.
Note: If you make a mistake during the follow-
ing procedure, it can be very difficult to correct.
Therefore, it is important to double check wheel
alignment (see Page 53), and troubleshoot all
other possible solutions (see Troubleshooting
on Page 48) prior to adjusting the lower wheel
shaft position.
Figure 71. Example of measuring the distance to
shim the wheel to be coplanar.
Remove blade.
4.
Remove wheel to be shimmed. Place as
5.
many shims as necessary to correct gap
measured in Step 3 onto wheel shaft.
-54-
Rear Adjustment
Bolts w/Hex Nuts
Figure 72. Location of rear lateral adjustment
components.
Model G0948 (Mfd. Since 08/21)
Page 58
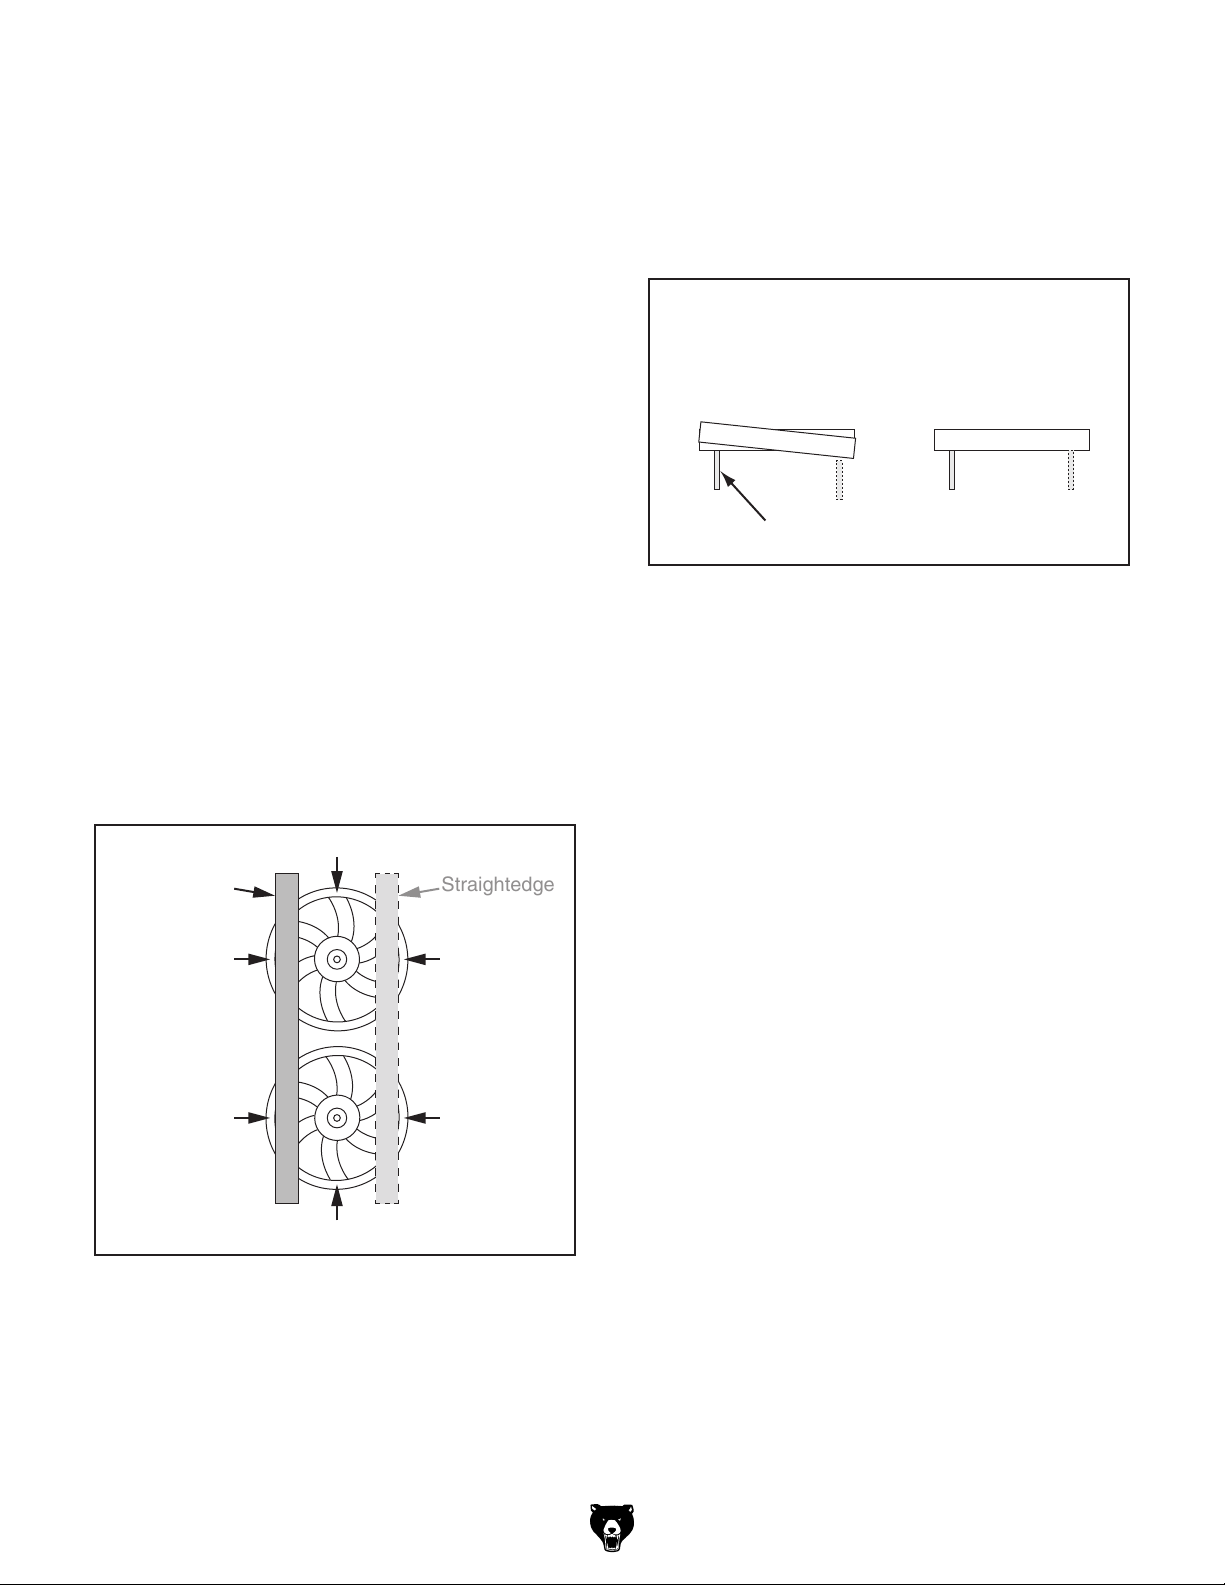
Item(s) Needed Qty
Straightedge
Precision Straightedge 3'. .................................. 1
Open-End Wrench or Socket 10mm
Pencil or Marker
................................................ 1
................. 1
To adjust lower wheel laterally:
1.
DISCONNECT MACHINE FROM POWER!
Remove fence and table from machine.
2.
5.
Loosen hex nuts on rear left and right adjust-
ment bolts (see Figure 72 on Page 54).
6.
Rotate left and right adjustment bolts until
lower wheel is coplanar with upper wheel,
see Figure 74.
Viewed From Above
Check wheels at A and B locations (see
3.
Figure 73). The wheels should align.
— If wheels align, no adjustment is required.
— If wheels do not align, they require lateral
adjustment (see Figure 74). Proceed to
Step 4.
Mark upper and lower wheels with a pencil or
4.
marker to indicate measuring locations (see
Figure 73).
Note: Marking the wheels ensures more
accurate results in case there are irregularities in the wheels.
Upper Wheel
Straightedge
Requires lateral
adjustment
After lateral
adjustment
Straightedge
Figure 74. Before and after lateral wheel
alignment (viewed from above).
7. Tighten hex nuts loosened in Step 5.
A1 B1
B2 A2
Lower Wheel
Figure 73. Example of using a straightedge to
check lateral wheel alignment.
Model G0948 (Mfd. Since 08/21)
-55-
Page 59
Blade Lead
Bandsaw blades may wander off the cut line when
sawing, as shown in Figure 75. This is called
blade lead.
Figure 75. Example of blade lead.
Skewing Fence
Item(s) Needed Qty
Hex Wrench 4mm. ............................................. 1
Scrap Wood
Clamp 4"
1. Cut a piece of scrap wood approximately 3⁄4"
thick x 3" wide x 17" long. On wide face of
board, draw a straight line parallel to long
edge.
Slide bandsaw fence out of way and cut
2.
along the line halfway through the board.
Turn bandsaw OFF and wait for blade to
stop. Do not move board.
Clamp board to bandsaw table, then slide
3.
fence over to board so it barely touches one
end of board.
4. Loosen fence adjustment cap screws, skew
fence so it is parallel with scrap piece, then
tighten cap screws.
3
⁄4" x 3" x 17" ................................. 1
............................................................ 1
Blade lead is usually caused by too fast of a
feed rate, a dull or abused blade, or improper
blade tension. If your blade is sharp/undamaged,
properly tensioned, and you still have blade lead,
perform the following procedures.
Correcting Blade Lead
1.
Make sure blade is properly tensioned, and
blade guides are adjusted correctly.
Use less pressure when feeding workpiece
2.
through cut.
Make sure miter slot and fence are parallel to
3.
blade line (see Aligning Table and Aligning
Fence procedures for detailed information).
Perform test cut with bandsaw.
4.
— If there is still blade lead present, com-
pensate for this condition by skewing
the fence, as instructed in the following
procedures.
Make a few cuts using fence.
5.
— If blade lead is still present, repeat
Steps 1–4 until blade and fence are parallel with each other.
-56-
Model G0948 (Mfd. Since 08/21)
Page 60
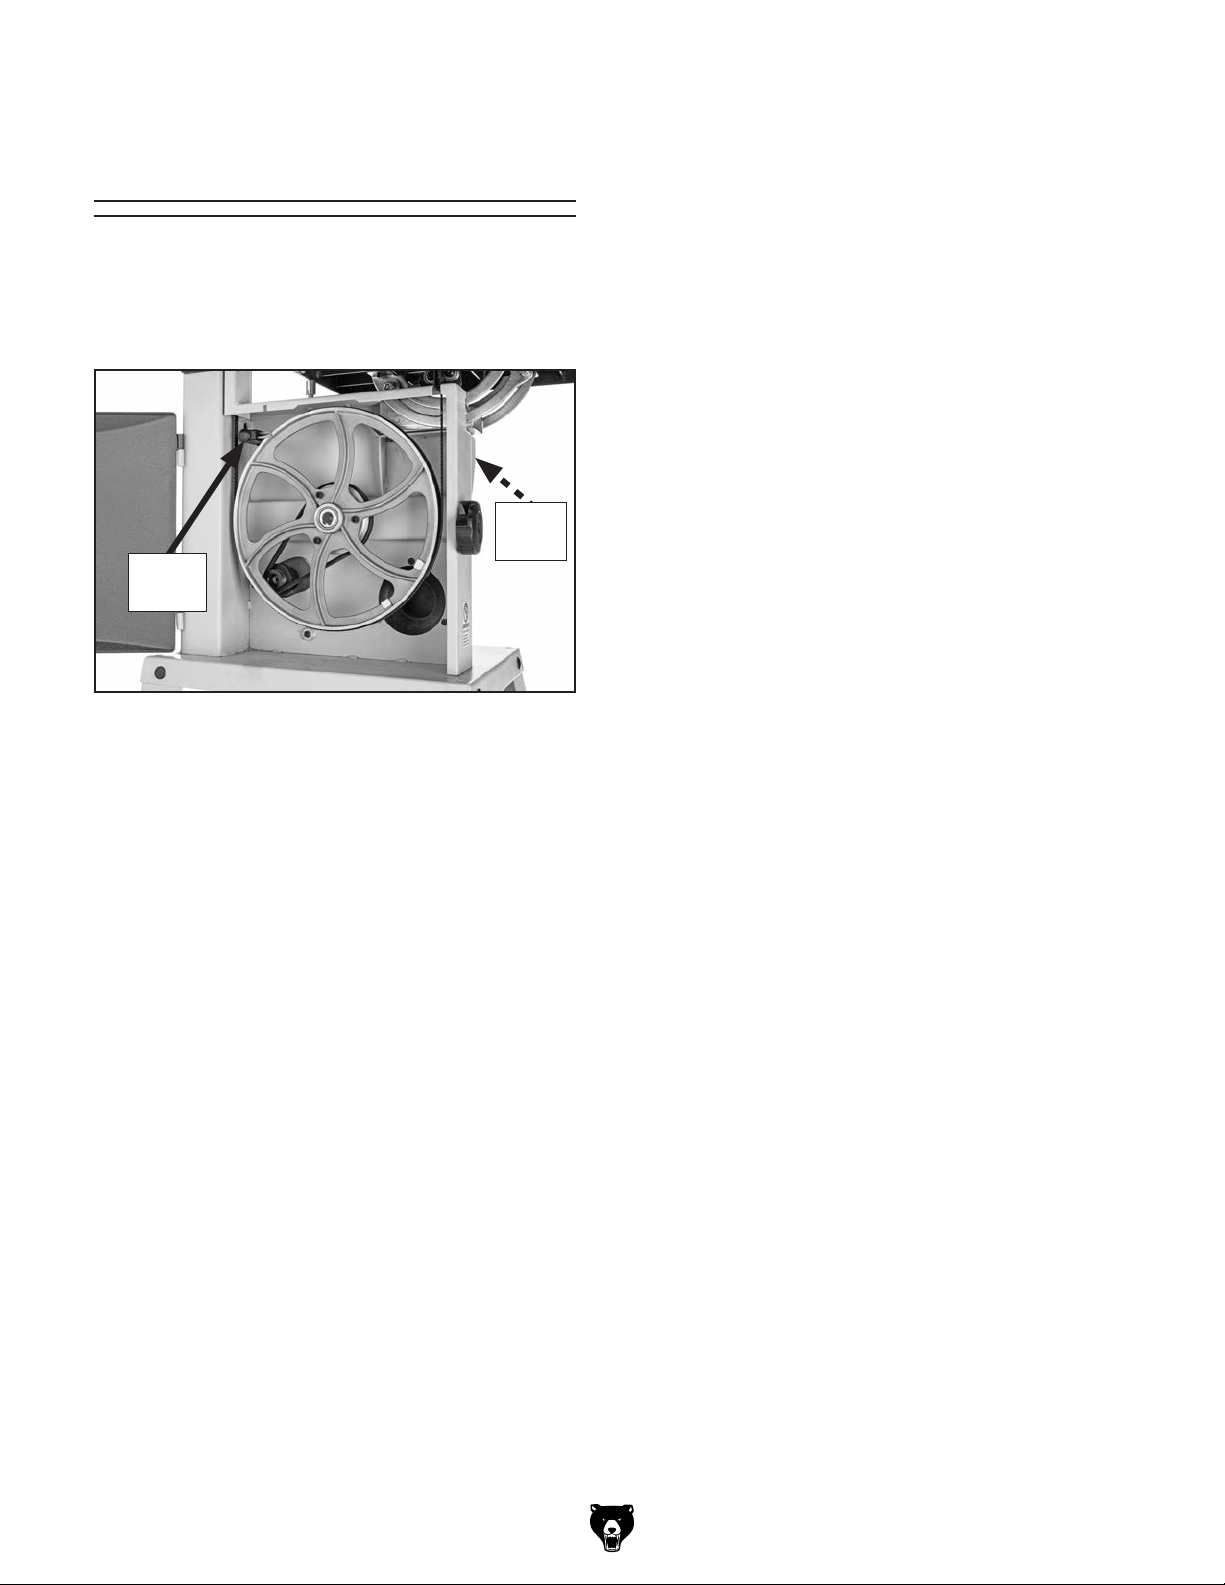
Adjusting
Tool(s) Needed: Qty
Wrench or Socket 13mm ................................... 1
Wheel Brush
The lower wheel has a brush (see Figure 76)
that is designed to sweep sawdust off the tire and
blade during operation. In order to work properly,
the brush must make firm contact with the tire.
Acorn
Nut
Wheel
Brush
Figure 76. Location of wheel brush.
To adjust wheel brush:
1. DISCONNECT MACHINE FROM POWER!
Open lower wheel cover.
2.
3. On rear of machine, loosen acorn nut
that secures wheel brush in position (see
Figure 76).
Adjust wheel brush so it makes firm, even
4.
contact with wheel without bending the bristles, then tighten acorn nut to secure wheel
brush in place.
Model G0948 (Mfd. Since 08/21)
-57-
Page 61
These pages are current at the time of printing. However, in the spirit of improvement, we may make changes to the electrical systems of future machines. Compare the manufacture date of your machine to the one
number and manufacture date of your
machine before calling. This information can be found on the main machine label.
machine
SECTION 8: WIRING
stated in this manual, and study this section carefully.
If there are differences between your machine and what is shown in this section, call Technical Support at
(570) 546-9663 for assistance BEFORE making any changes to the wiring on your machine. An updated
wiring diagram may be available. Note: Please gather the serial
Wiring Safety Instructions
SHOCK HAZARD. Working on wiring that is con-
nected to a power source is extremely dangerous.
Touching electrified parts will result in personal
injury including but not limited to severe burns,
electrocution, or death. Disconnect the power
from the machine before servicing electrical components!
MODIFICATIONS. Modifying the wiring beyond
what is shown in the diagram may lead to unpredictable results, including serious injury or fire.
This includes the installation of unapproved aftermarket parts.
WIRE CONNECTIONS. All connections must
be tight to prevent wires from loosening during
machine operation. Double-check all wires disconnected or connected during any wiring task to
ensure tight connections.
CIRCUIT REQUIREMENTS. You MUST follow
the requirements at the beginning of this manual
when connecting your machine to a power source.
WIRE/COMPONENT DAMAGE. Damaged wires
or components increase the risk of serious personal injury, fire, or machine damage. If you notice
that any wires or components are damaged while
performing a wiring task, replace those wires or
components.
MOTOR WIRING. The motor wiring shown in
these diagrams is current at the time of printing
but may not match your machine. If you find this
to be the case, use the wiring diagram inside the
motor junction box.
CAPACITORS/INVERTERS. Some capacitors
and power inverters store an electrical charge for
up to 10 minutes after being disconnected from
the power source. To reduce the risk of being
shocked, wait at least this long before working on
capacitors.
EXPERIENCING DIFFICULTIES. If you are experiencing difficulties understanding the information
included in this section, contact our Technical
Support at (570) 546-9663.
The photos and diagrams
included in this section are
best viewed in color. You
can view these pages in
color at www.grizzly.com.
-58-
Model G0948 (Mfd. Since 08/21)
Page 62
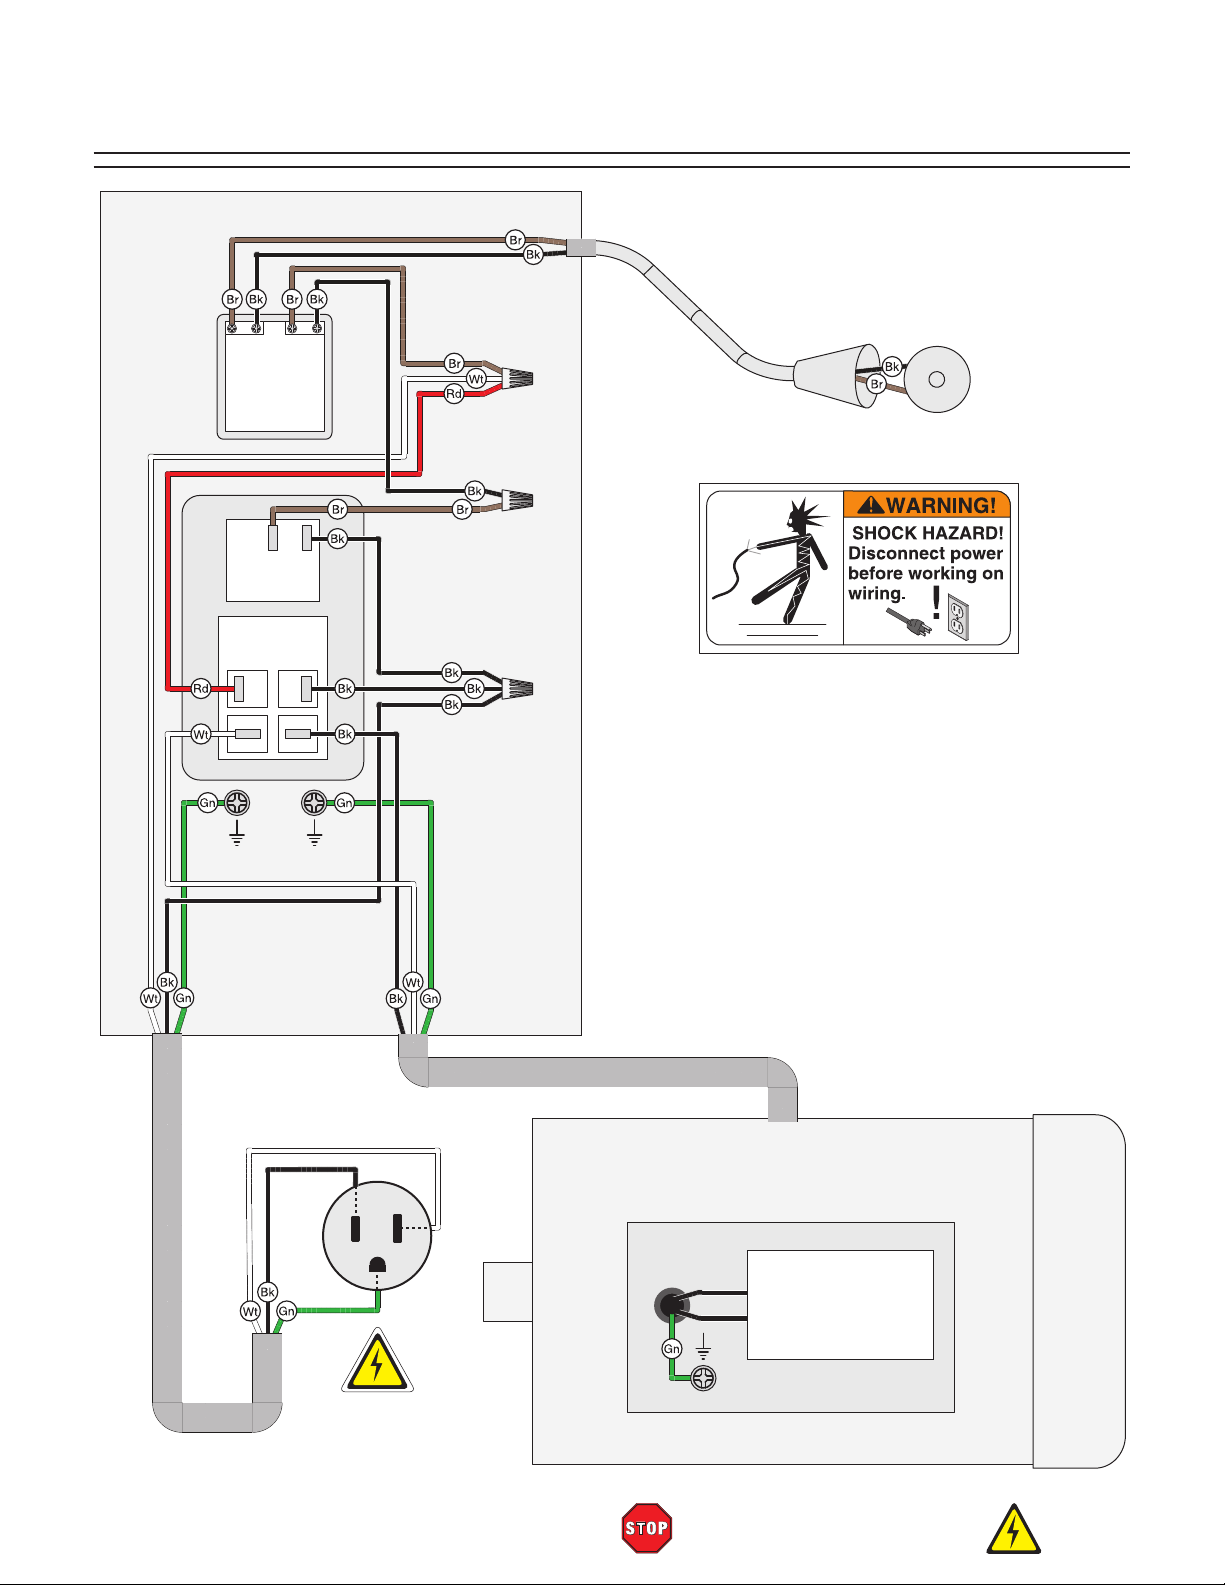
wiring diagram
Wiring Diagram
Bandsaw Body
+
–
LED Driver
LED-5V700
Hopestar
120V ~ 5.5W
E337681
Light Switch
DKLD AN-18
250V 6A
ON/OFF Switch
DKLD AN17
125V 20A
Ground Ground
N
L
LED Light
Nanjing
12V 1W
Neutral
Hot
Ground
120VAC
5-15 Plug
Model G0948 (Mfd. Since 08/21)
120V Motor
Start Capacitor
CBB60 35uF
350VAC
Ground
READ ELECTRICAL SAFETY
ON PAGE 58!
-59-
Page 63
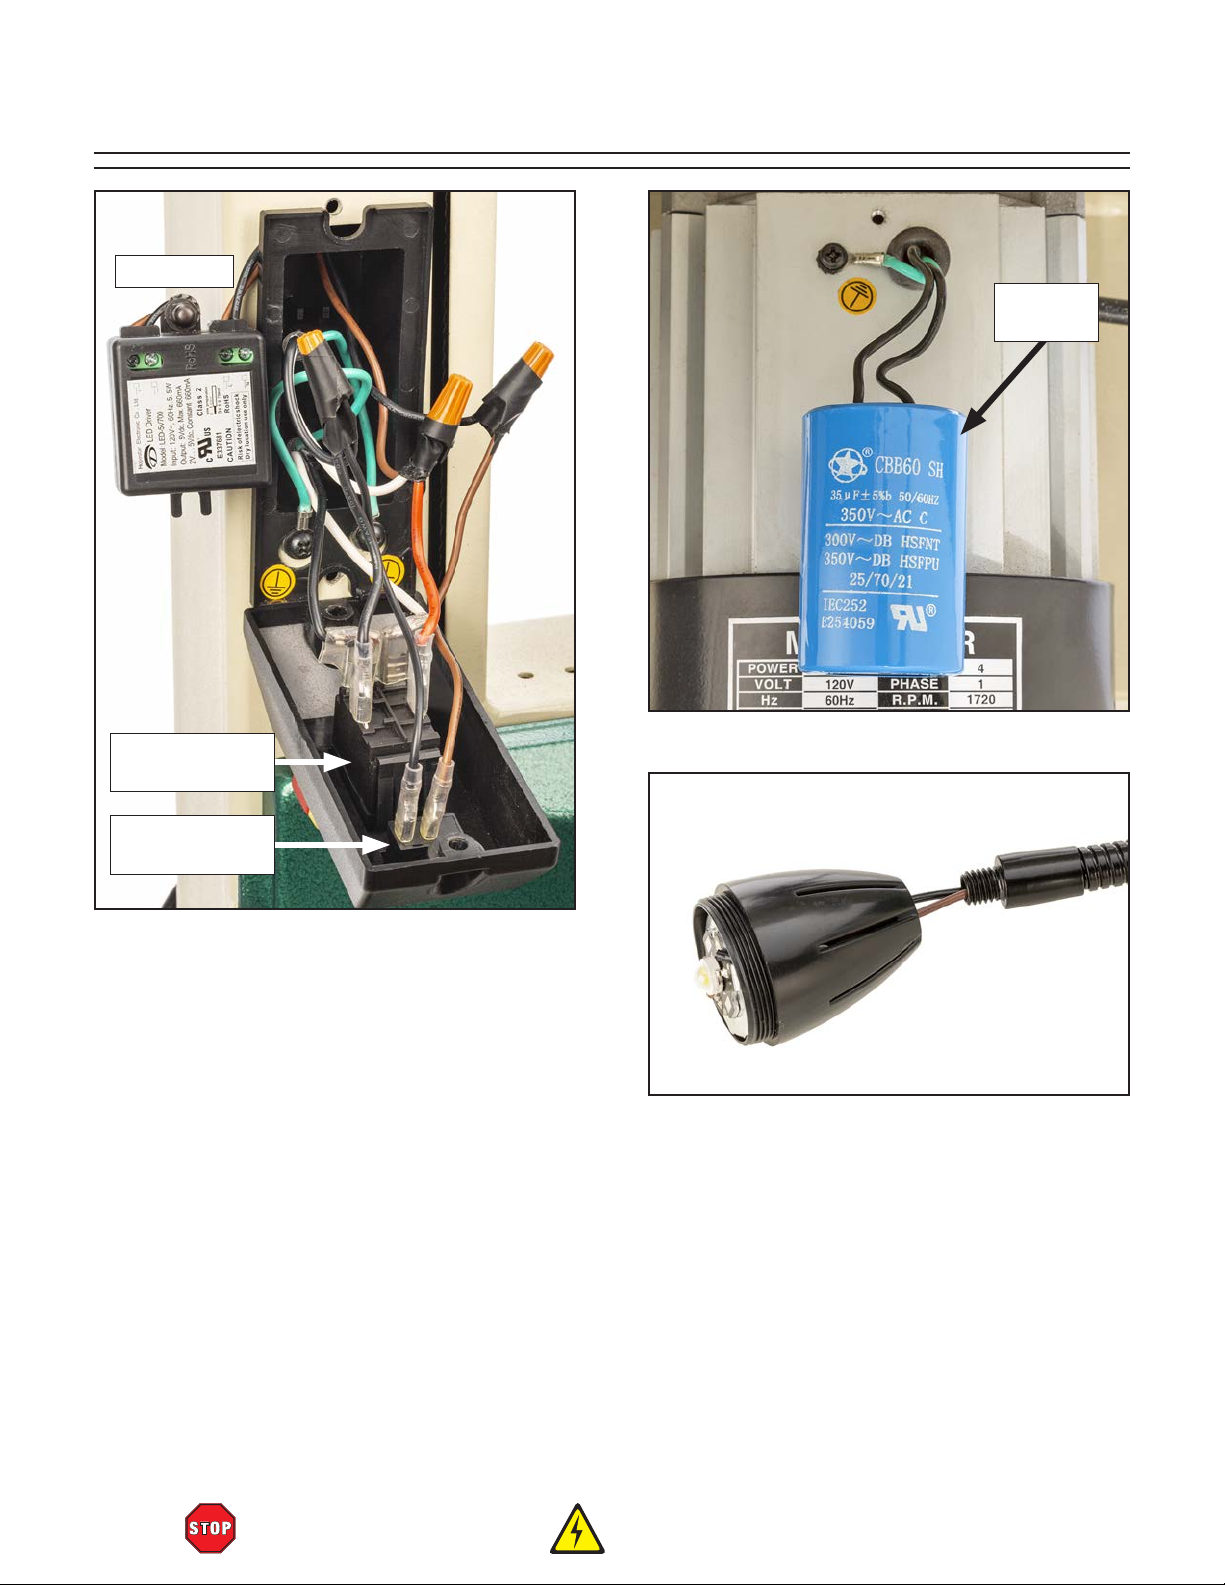
LED Driver
Electrical Components
Start
Capacitor
Power
ON/OFF Switch
LED Light
ON/OFF Switch
Figure 77. ON/OFF switch wiring.
Figure 78. Start capacitor wiring.
Figure 79. Work light wiring.
-60-
READ ELECTRICAL SAFETY
ON PAGE 58!
Model G0948 (Mfd. Since 0 8/21)
Page 64
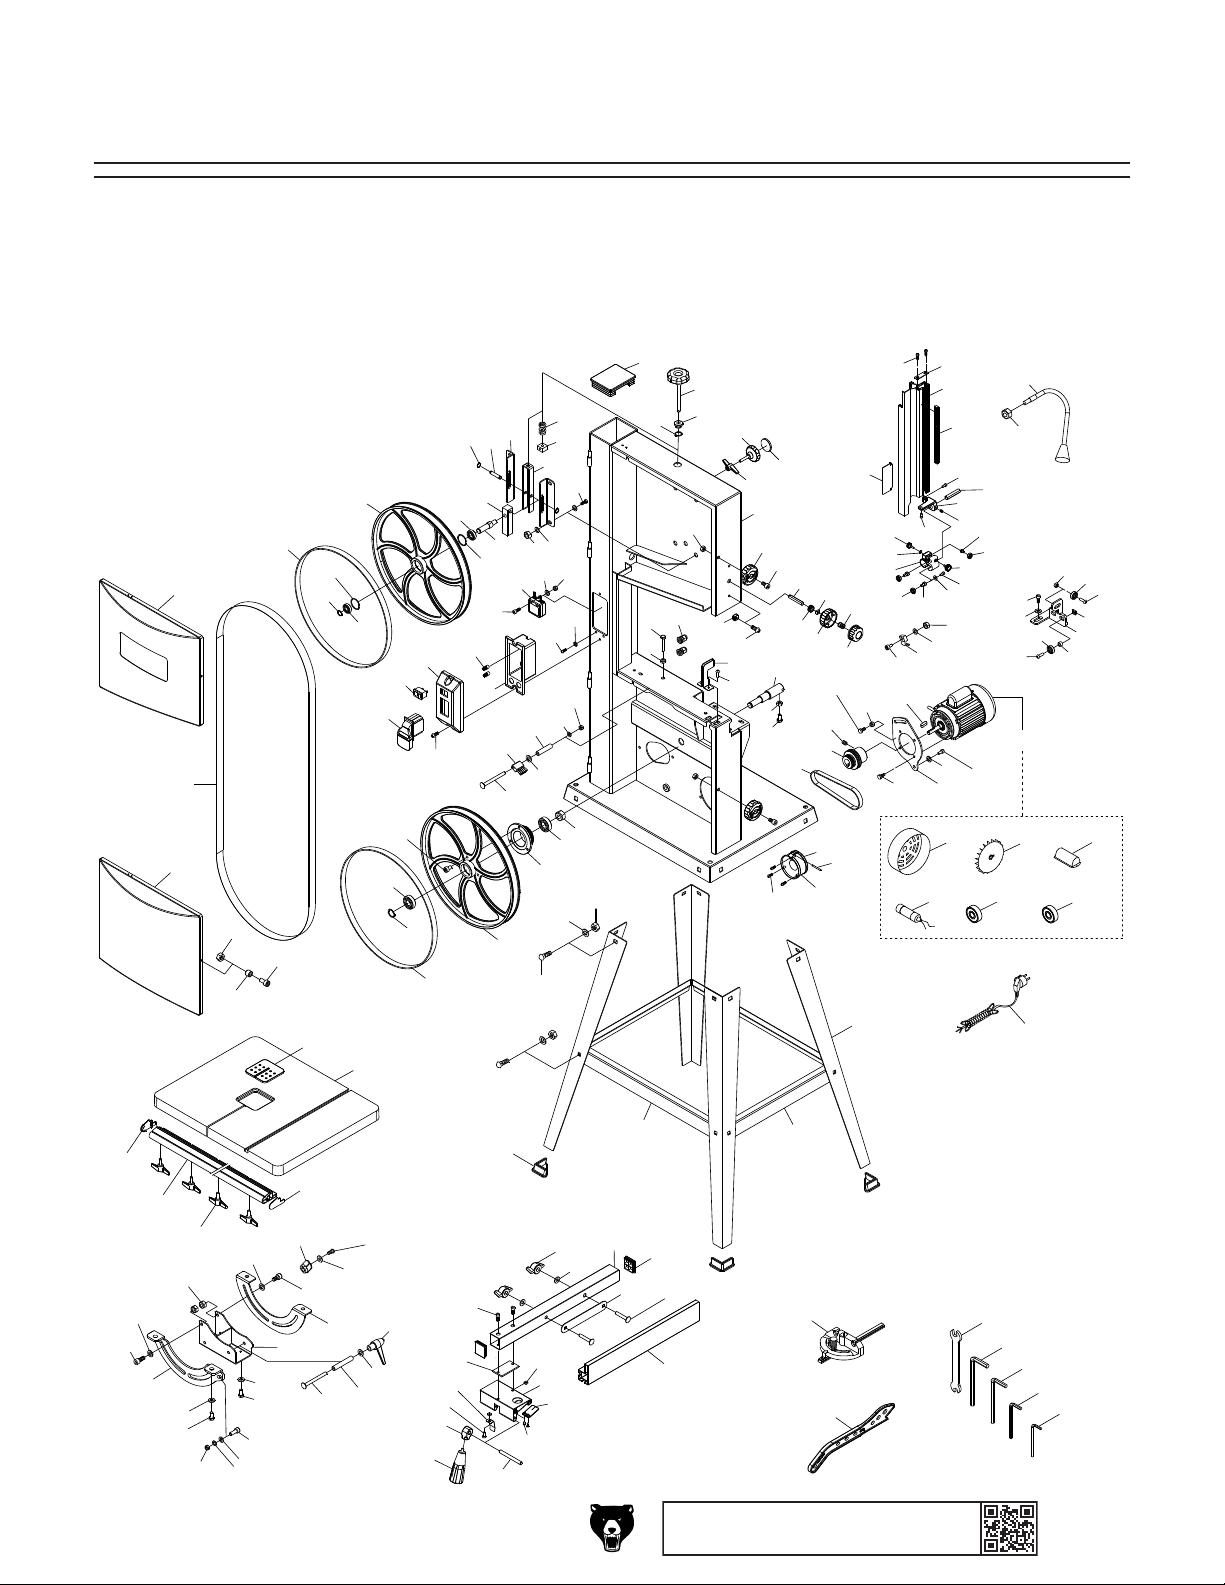
SECTION 9: PARTS
We do our best to stock replacement parts when possible, but we cannot guarantee that all parts shown
are available for purchase. Call (800) 523-4777 or visit www.grizzly.com/parts to check for availability.
Main
22
23
21
24
25
26
20
19
118
17
18
16
119
38
16
37
48
19
36
20
39
16
7
35
14
17
34
8
15
31
18
30
44
9
45
13
29
42
165
166
10
43
47
12
33
41
16
5
6
11
28
32
40
46
164
4
50
51
71
72
1
2
3
49
57
55
53
56
66
67
54
58
69
70
52
27
59
68
105
112
61
60
104
62
63
102
103
114
113
75
64
65
101
115
81
82
83
90
106
167
140
110
73
80
88
89
138
139
108
107
111-4
137
142
74
141
76
77
78
79
84
85
86
87
99
100
97
98
111
109
111-2111-1 111-3
111-5 111-6
116
91
92
93
94
95
96
146
168
145
148
147
149
BUY PARTS ONLINE AT GRIZZLY.COM!
Scan QR code to visit our Parts Store.
170
152
125
124
178
151
130
131
117
176
136
177
125
135
138
132
133
150
123
128
124
129
122
126
127
121
134
125
160
161
162
158
157
159
143
144
156
155
154
153
163
Model G0948 (Mfd. Since 08/21)
169
120
171
172
173
179
174
175
-61-
Page 65
Main Parts List
REF PART # DES CRIPTI ON REF PART # DES CRIPTI ON
1 P0948001 KNOB BOLT M8-1.25 X 10², 6-LOBE, D60 53 P0948053 KNOB BOLT M8-1.25 X 42, 8-LOBE, D60
2 P0948002 BUS HI NG 54 P0948054 KNOB M8-1.25, D72, WING
3 P0948003 EX T RETAI NI NG RI NG 1 5MM 55 P0948055 GUIDE BLOCK M4-.7
4 P0948004 FRAME CAP 56 P0948056 PHLP HD SCR M4-.7 X 8
5 P0948005 COMPRESSION SPRI NG 4 X 19 X 30 57 P0948057 LO CK NUT M6-1
6 P0948006 TENS I ON NUT M8- 1. 25 58 P0948058 KNOB 6MM, 10-LOBE, D55
7 P0948007 EX T RETAI NI NG RI NG 8 MM 59 P0948059 CAP SCREW M6-1 X 16
8 P0948008 SHA FT 60 P0948060 THREADED SHAFT M8-1.25 X 12, 38L
9 P0948009 GUIDE PLATE 61 P0948061 GEAR 15T
10 P0948010 PULLING PLATE 62 P0948062 BUSHI NG
11 P0948011 HEX BOLT M8-1.25 X 16 63 P0948063 KNOB 8MM, 10-LOBE, D50
12 P0948012 FLAT WAS HER 8MM 64 P0948064 COMPRESSION SPRING 1.6 X 22 X 25
13 P0948013 HEX NUT M8- 1.25 65 P0948065 KNOB COVER
14 P0948014 TENSION BLOCK 66 P0948066 LOWER BLADE GUARD
15 P0948015 SHAFT 67 P0948067 CAP SCREW M6-1 X 10
16 P0948016 BALL BEARING 6000ZZ 68 P0948068 LOWER WHEEL SPINDLE
17 P0948017 INT RETA I NI NG RI NG 26MM 69 P0948069 HEX NUT M6- 1
18 P0948018 WHEEL 10" 70 P0948070 HEX BOLT M6-1 X 20
19 P0948019 EXT RETA I NI NG RI NG 10MM 71 P0948071 TAP SCREW 4.8 X 13
20 P0948020 TIRE 72 P0948072 PLATE
21 P0948021 SAW BLADE 72" X 3/8" 6-TPI HOOK 73 P0948073 UPPER BLADE GUIDE ASSEMBLY
22 P0948022 UPPER WHEEL COVER 74 P0948074 RACK
23 P0948023 LOWER WHEEL COVER 75 P0948075 SLIDING COVER
24 P0948024 LOCK NUT M6 -1 76 P0948076 CAP SCREW M5-.8 X 6
25 P0948025 SPACER 77 P0948077 CONNECTI NG SHAFT
26 P0948026 CAP SCREW M6-1 X 16 78 P0948078 SUPPORT BLOCK
27 P0948027 FRAME 79 P0948079 SET SCREW M6-1 X 8
28 P0948028 HEX NUT M4- . 7 80 P0948080 TAP SCREW M8 X 13
29 P0948029 FLAT WAS HER 4MM 81 P0948081 KNOB BOLT M5-.8 X 22, 4-LOBE, D22
30 P0948030 LED DRIVER HOPESTAR LED-5V700 120V 5.5W 82 P0948082 FLAT WAS HER 5MM
31 P0948031 CAP SCREW M4-.7 X 12 83 P0948083 BEARING SUPPORT
32 P0948032 INT TOO TH WASHE R 5MM 84 P0948084 T-SLO T NUT M5-. 8
33 P0948033 PHLP HD SCR M5-.8 X 12 85 P0948085 BALL BEARING 607ZZ
34 P0948034 SWI TCH B OX 86 P0948086 KNOB BOLT M5-.8 X 8, 4-LOBE, D22
35 P0948035 WIRE NUT 1 8G 87 P0948087 CAP SCREW M5-.8 X 16
36 P0948036 SWITCH BOX COVER 88 P0948088 FL AT WASHER 5 MM
37 P0948037 ON/OFF SWITCH DKLD AN-18 250V 6A 89 P0948089 T-SLO T NUT M5-. 8
38 P0948038 ON/OFF SWITCH DKLD AN17 125V 20A 90 P0948090 BALL BEARING 607ZZ
39 P0948039 PHLP HD SCR M5-.8 X 10 91 P0948091 HEX NUT M6- 1
40 P0948040 HEX NUT M8- 1.25 92 P0948092 BALL BEARING 626ZZ
41 P0948041 FLAT WAS HER 8MM 93 P0948093 CAP SCREW M6-1 X 16
42 P0948042 BUSHI NG 94 P0948094 S QUARE NUT M6- 1
43 P0948043 FLAT WAS HER 8MM 95 P0948095 GUIDE PLATE
44 P0948044 BRUSH 96 P0948096 BUSHI NG
45 P0948045 CARRIAGE BOLT M8-1.25 X 70 97 P0948097 BALL BEARING 626ZZ
46 P0948046 HEX NUT M14 -2 98 P0948098 CAP SCREW M6-1 X 20
47 P0948047 WHEEL PULLEY 99 P0948099 CAP SCREW M6-1 X 10
48 P0948048 CAP SCREW M5-.8 X 10 100 P0948100 FLA T WASHER 6MM
49 P0948049 STRAIN RELIEF TYPE-3 M16-1.5 101 P0948101 HEX NUT M6-1
50 P0948050 STOP BOLT M8-1.25 X 22 102 P0948102 HEX BOLT M6-1 X 20
51 P0948051 HEX NUT M8- 1.25 103 P0948103 SET SCREW M6-1 X 8
52 P0948052 KNOB COVER 104 P0948104 MOTOR PULLEY
-62-
BUY PARTS ONLINE AT GRIZZLY.COM!
Scan QR code to visit our Parts Store.
Model G0948 (Mfd. Since 08/21)
Page 66
Main Parts List (Cont.)
REF P ART # DESCRI PTIO N REF P ART # DES CRIPTI ON
105 P0948105 POLY V-BELT PT400 140 P0948140 CAP SCREW M5-.8 X 12
106 P0948106 HEX BOLT M6-1 X 16 141 P0948141 HEX NUT M10-1 . 5
107 P0948107 MOTOR MO UNTI NG PL ATE 142 P0948142 LED LIGHT NANJI NG 12V 1W
108 P0948108 FLAT WA SHER 8MM 143 P0948143 KNOB M6-1, D32, WING
109 P0948109 CAP SCREW M8-1.25 X 20 144 P0948144 FLAT WAS HER 6MM
110 P0948110 KEY 5 X 5 X 25 RE 145 P0948145 FENCE CA P
111 P0948111 MOTOR 1/ 2HP 120V 1-PH 146 P0948146 FENCE SUPPORT
111-1 P0948111-1 MOTOR FAN COVE R 147 P0948147 GUIDE PLATE
111-2 P0948111-2 MOTOR FAN 148 P0948148 CARRI AGE BOLT M6-1 X 55
111-3 P0948111-3 CAPACITOR COVER 149 P0948149 FENCE
111-4 P0948111-4 S CAPACITOR 35M 350V 1-5/8 X 2-1/2 150 P0948150 FENCE RAI L CAP ( RI GHT)
111-5 P0948111-5 BALL BEARING 6202ZZ (FRONT) 151 P0948151 FENCE RA I L
111-6 P0948111-6 BALL BEARING 6201ZZ (REAR) 152 P0948152 FENCE RAI L CAP (LEFT)
112 P0948112 TAP SCREW M4.2 X 13 153 P0948153 TAP SCREW M2.9 X 9. 5
113 P0948113 DUST PO RT 154 P0948154 POINTER
114 P0948114 DUST PO RT COVER 155 P0948155 FENCE BASE
115 P0948115 ROLL PIN 3 X 22 156 P0948156 SQUA RE NUT M5-. 8
116 P0948116 POWER CORD 18G 3W 72" 5-15P 157 P0948157 SPACER
117 P0948117 KNOB BOLT M8-1. 25 X 18, D72, WING 158 P0948158 CAP SCREW M5-.8 X 10
118 P0948118 TABLE INSERT 159 P0948159 SPRING PLATE
119 P0948119 TABLE 160 P0948160 PHLP HD SCR M5-.8 X 8
120 P0948120 MITE R GAUGE 161 P0948161 FENCE HANDLE LOCKING CAM
121 P0948121 PHLP HD SCR M4-.7 X 12 162 P0948162 KNOB BOLT M6-1 X 10, D35, TAPERED
122 P0948122 FLAT WA SHER 4MM 163 P0948163 SHAFT
123 P0948123 POINTER 164 P0948164 HEX NUT M8 -1. 25
124 P0948124 SHOULDER SCREW M8-1. 25 X 12, 8 X 8 165 P0948165 FLAT WA SHER 8MM
125 P0948125 FLAT WA SHER 8MM 166 P0948166 CARRIAGE BOLT M8-1.25 X 16
126 P0948126 TRUNNIO N (REAR) 167 P0948167 LEG
127 P0948127 BUSHI NG 168 P0948168 LONG BRACE
128 P0948128 TRUNNIO N BRACKET 169 P0948169 SHORT BRACE
129 P0948129 CARRI AGE BOLT M8-1.25 X 70 170 P0948170 FOOT
130 P0948130 FLAT WA SHER 6MM 171 P0948171 WRENCH 10 X 13MM OPEN-ENDS
131 P0948131 HEX BOLT M6-1 X 10 172 P0948172 HEX WRENCH 6MM
132 P0948132 FLAT WA SHER 6MM 173 P0948173 HEX WRENCH 5MM
133 P0948133 HEX BOLT M6-1 X 12 174 P0948174 HEX WRENCH 4MM
134 P0948134 ADJ HANDLE M8-1.25 , 72L 175 P0948175 HEX WRE NCH 3MM
135 P0948135 CAP SCREW M5-.8 X 12 176 P0948176 LOCK NUT M8-1.25
136 P0948136 HEX NUT M5 -.8 177 P0948177 LOCK WASHER 5MM
137 P0948137 HEX NUT M5 -.8 178 P0948178 TRUNNIO N (FRONT)
138 P0948138 FLAT WA SHER 5MM 179 P0948179 PUSH STI CK
139 P0948139 CORD CLAMP 3/8"
Model G0948 (Mfd. Since 08/21)
BUY PARTS ONLINE AT GRIZZLY.COM!
Scan QR code to visit our Parts Store.
-63-
Page 67
Labels & Cosmetics
REF PART # DE SCRIPTION REF P ART # DESCRIP TION
grizzly.com
G0948
201
202
203
INJURY/SHOCK
HAZARD!
Disconnect power
before adjustments,
maintenance, or
service.
211
205
210
WARNING!
EYE/LUNG INJURY
HAZARD!
Always wear safety
glasses and a
respirator when
using this machine.
209
207
WARNING!
To reduce risk of death
or serious injury, read
manual BEFORE using
machine.
To get a new manual,
call (800) 523-4777 or
go to www.grizzly.com.
208
Specifications
Motor: 1/2 HP, 120V, 1-Ph, 60Hz
Full Load Amp Draw: 3.5A
Blade Speed: 1520, 2620 FPM
Standard Blade Length: 72"
Blade Length Range: 71-1/2"–72-1/2"
Blade Width Range: 1/8"–1/2"
Max. Cutting Width Left of Blade: 9-3/4"
Max. Cutting Height: 6-1/8"
Table Size: 14-3/16" x 12-5/8"
Table Tilt: 0˚L ⁄ 45˚R
Weight: 69 lbs.
Date
S/N
Mfd. for Grizzly in China
206
INJURY HAZARD!
Do not open door
while machine is
connected to power
or blade is in motion.
MODEL G0948
10" 1/2 HP BANDSAW
To reduce risk of serious injury when using this machine:
1. Read and understand owner’s manual before operating.
2. Never touch moving blade. Keep hands out of blade path.
3. Always wear approved eye protection and respirator.
4. Only plug power cord into a grounded outlet.
5. Only remove jammed cutoff pieces when blade is stopped.
6. Use push stick or holding jig to cut small or narrow pieces.
7. Disconnect power before changing blades or adjusting saw.
8. Maintain adjustment of blade tension, tracking, and guides.
9. Keep upper guide adjusted to just clear the workpiece.
10. Hold workpiece firmly against table to maintain control.
11. Only run saw with wheel covers closed and all guards in place.
12. Never reach under table while blade is in motion.
13. Remove/secure loose clothing and long hair.
14. DO NOT expose to rain or use in wet locations.
15. Prevent unauthorized use by children or untrained users;
WARNING!
restrict access or disable machine when unattended.
204
205
201 P0948201 MODEL NUMBER LABEL 207 P0948207 READ MANUAL LABEL
202 P0948202 GRIZZLY INDUSTRIAL LOGO LABEL 208 P0948208 MACHINE ID LABEL
203 P0948203 DISCONNECT POWER LABEL 209 P0948209 GRIZZLY.COM LABEL
204 P0948204 TOUCH-UP P AI NT, GRI ZZLY G REEN 210 P0948210 EYE/LUNG INJURY LABEL
205 P0948205 ELECTRICITY LABEL 211 P0948211 TOUCH-UP P AI NT, GRI ZZLY B EIGE
206 P0948206 DO NOT OPEN DOOR LABEL
Safety labels help reduce the risk of serious injury caused by machine hazards. If any label comes
off or becomes unreadable, the owner of this machine MUST replace it in the original location
before resuming operations. For replacements, contact (800) 523-4777 or www.grizzly.com.
-64-
BUY PARTS ONLINE AT GRIZZLY.COM!
Scan QR code to visit our Parts Store.
Model G0948 (Mfd. Since 08/21)
Page 68
WARRANTY & RETURNS
Grizzly Industrial, Inc. warrants every product it sells for a period of 1 year to the original purchaser from
the date of purchase. This warranty does not apply to defects due directly or indirectly to misuse, abuse,
negligence, accidents, repairs or alterations or lack of maintenance. This is Grizzly’s sole written warranty
and any and all warranties that may be implied by law, including any merchantability or fitness, for any particular purpose, are hereby limited to the duration of this written warranty. We do not warrant or represent
that the merchandise complies with the provisions of any law or acts unless the manufacturer so warrants.
In no event shall Grizzly’s liability under this warranty exceed the purchase price paid for the product and
any legal actions brought against Grizzly shall be tried in the State of Washington, County of Whatcom.
We shall in no event be liable for death, injuries to persons or property or for incidental, contingent, special,
or consequential damages arising from the use of our products.
The manufacturers reserve the right to change specifications at any time because they constantly strive to
achieve better quality equipment. We make every effort to ensure that our products meet high quality and
durability standards and we hope you never need to use this warranty.
In the event you need to use this warranty, contact us by mail or phone and give us all the details. We will
then issue you a “Return Number,’’ which must be clearly posted on the outside as well as the inside of
the carton. We will not accept any item back without this number. Proof of purchase must accompany the
merchandise.
Please feel free to write or call us if you have any questions about the machine or the manual.
Thank you again for your business and continued support. We hope to serve you again soon.
To
you can
applicable information for
take advantage of this warranty, you must register it at https://www.grizzly.com/forms/warranty, or
scan the QR code below to be automatically directed to our warranty registration page. Enter all
the product.
WARRANTY
Page 69
 Loading...