

Page 1
OPERATION MANUAL
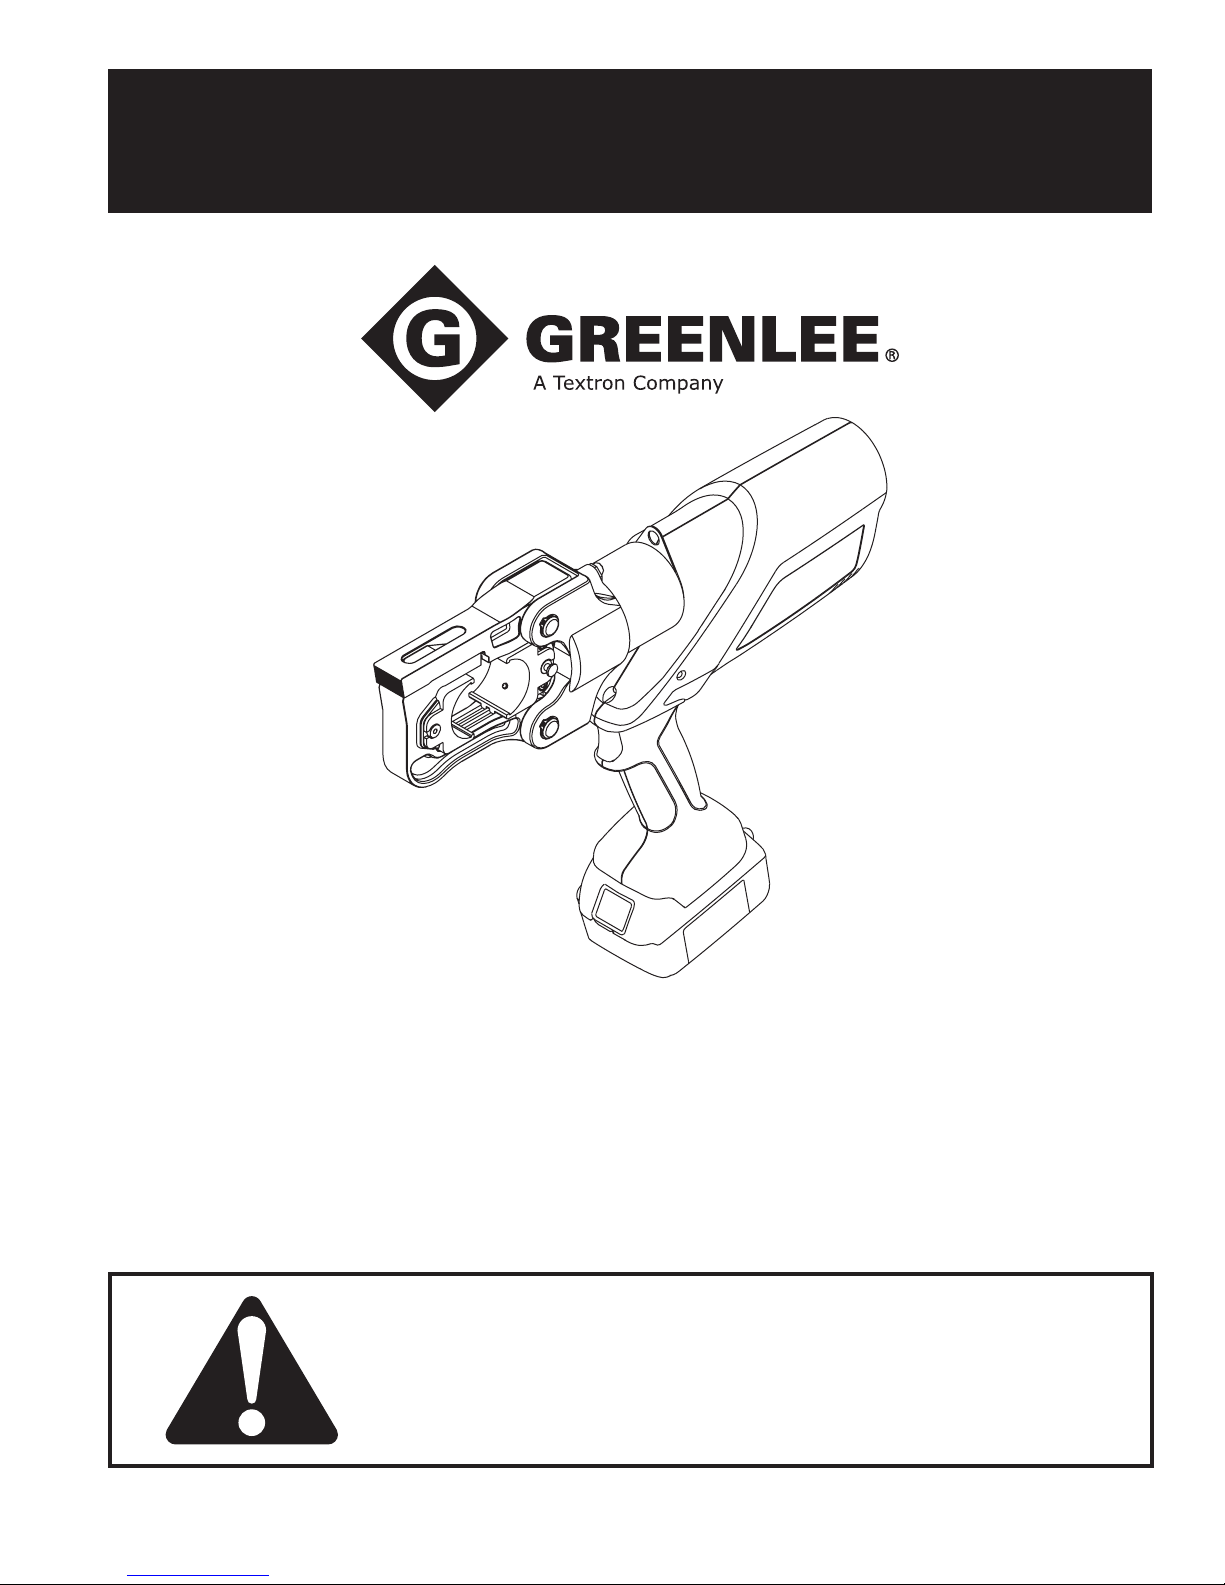
GATOR® E12CCXL
Battery-powered Tool
Read and understand all of the instructions and
safety information in this manual before operating
or servicing this tool.
52047655 REV 9 © 2016 Greenlee Textron Inc. 7/16
12-ton
Register this product at www.greenlee.com
Page 2
E12CCXL 12-ton Battery-powered Tool
Table of Contents
Description .................................................................... 2
Safety ............................................................................ 2
Purpose of this Manual ................................................. 2
Important Safety Information .....................................3–4
Identication .................................................................. 5
Specications ................................................................ 5
Operation ..................................................................6–15
Crimping Using KC12 or KA12 type U-style Dies...7–8
Crimping Using UA12ID Dieless Die Set ................... 9
Cutting ..................................................................... 10
Punching .............................................................11–15
Die Selection ............................................................... 15
Connector Selection .................................................... 15
Additional U-type Dies ................................................ 16
Available Accessories .................................................. 16
cUL and UL Classied Crimps .................................... 18
Connector Table .......................................................... 18
Maintenance ................................................................ 19
Troubleshooting ........................................................... 20
Description
The E12CCXL 12-ton Battery-powered, High-speed Tool
is a hand-held, self-contained tool intended to crimp
cable, cut cable and threaded rod, and punch holes with
the proper adapters.
This tool has a retraction stop feature which allows the
operator to stop the retraction motion of the ram to
shorten cycle time.
This tool is protected by U.S. Patent No. 6,206,663,
6,276,186, 6,401,515, 6,532,790, and 6,718,870.
Safety
Safety is essential in the use and maintenance of
Greenlee tools and equipment. This manual and any
markings on the tool provide information for avoiding
hazards and unsafe practices related to the use of this
tool. Observe all of the safety information provided.
Purpose of this Manual
This manual is intended to familiarize all personnel with
the safe operation and maintenance procedures for the
following Greenlee tool:
E12CCXL 12-ton Battery-powered,
High-speed Tool
Keep this manual available to all personnel.
Replacement manuals are available upon request at
no charge at www.greenlee.com.
Do not discard this product or throw away!
For recycling information, go to www.greenlee.com.
All specications are nominal and may change as design
improvements occur. Greenlee Textron Inc. shall not be liable for
damages resulting from misapplication or misuse of its products.
GATOR and Kwik Stepper are registered trademarks of Textron
Innovations Inc.
Blackburn is a registered trademark of Thomas & Betts.
KEEP THIS MANUAL
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
2
Page 3
IMPORTANT SAFETY INFORMATION
SAFETY
ALERT
SYMBOL
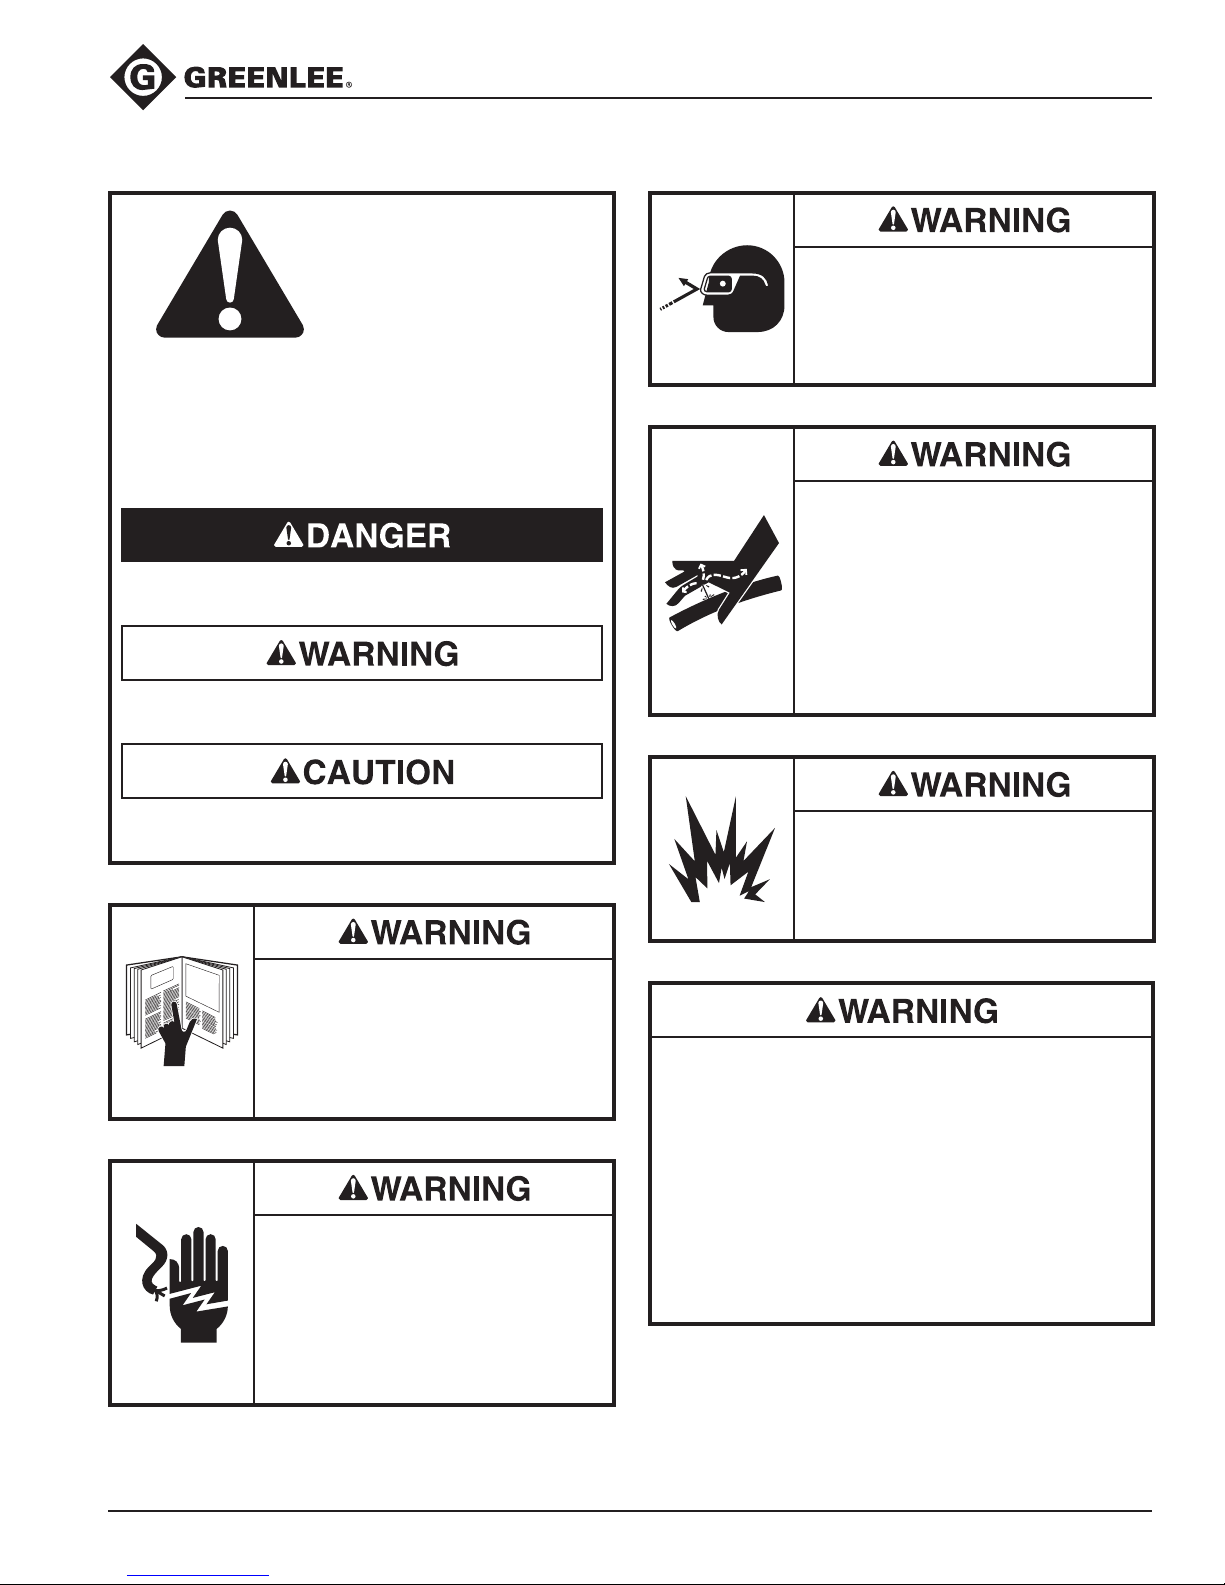
This symbol is used to call your attention to hazards
or unsafe practices which could result in an injury or
property damage. The signal word, dened below,
indicates the severity of the hazard. The message
after the signal word provides information for preventing or avoiding the hazard.
Immediate hazards which, if not avoided, WILL result
in severe injury or death.
Hazards which, if not avoided, COULD result in
severe injury or death.
E12CCXL 12-ton Battery-powered Tool
Wear eye protection when operating
or servicing this tool.
Failure to wear eye protection could
result in serious eye injury from
ying debris or hydraulic oil.
Skin injection hazard:
Do not use hands to check for oil
leaks. Oil under pressure easily
punctures skin. If injured, seek
medical attention immediately to
remove oil.
Failure to observe this warning
could result in serious injury, gangrene, or death.
Hazards or unsafe practices which, if not avoided,
MAY result in injury or property damage.
Read and understand all of the
instructions and safety information
in this manual before operating or
servicing this tool.
Failure to observe this warning
could result in severe injury or death.
Electric shock hazard:
This tool is not insulated. When
using this unit on or near energized
electrical lines, use proper personal
protective equipment.
Failure to observe this warning
could result in severe injury or death.
Do not use solvents or ammable
liquids to clean the tool body.
Solvents or ammable liquids could
ignite and cause serious injury or
property damage.
An incomplete crimp can cause a re.
• Use proper die, connector, and cable combinations. Improper combinations can result in an
incomplete crimp.
• The relief valve sounds and the ram automatically
retracts to indicate a completed crimp. If you do
not hear the sound of the relieve valve or the ram
does not automatically retract, the crimp is not
complete.
Failure to observe these warnings could result in
severe injury or death.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
3
Page 4
E12CCXL 12-ton Battery-powered Tool
IMPORTANT SAFETY INFORMATION
Pinch points:
• Remove battery before changing
dies, adapters, or jaws.
• Keep hands away from the crimping tool head when crimping.
Failure to observe these warnings
could result in severe injury or death.
Do not dispose of batteries in a re. They will vent
fumes and may explode.
Failure to observe this warning could result in severe
injury from harmful fumes or burns from ying
debris.
• Inspect tool and dies before use. Replace any
worn or damaged parts. A damaged or improperly assembled tool can break and strike nearby
personnel.
• Carrying strap is for carrying only, not to be used
to hang or suspend tool.
Failure to observe these warnings could result in
severe injury or death.
Do not allow anything to contact the battery
terminals.
• Do not immerse the batteries in liquid. Liquid may
create a short circuit and damage the battery.
If batteries are immersed, contact your service
center for proper handling.
• Do not place the battery into a pocket, tool pouch,
or tool box with conductive objects. Conductive
objects may create a short circuit and damage the
battery.
• Do not place a battery on moist ground or grass.
Moisture may create a short circuit and damage
the battery.
Failure to observe these precautions may result in
injury or property damage.
• Do not store the battery at more than 122 °F
(50°C) or less than –4 °F (–20 °C). Damage to the
battery can result.
• Do not use another manufacturer’s charger. Other
manufacturers’ chargers may overcharge and
damage the battery.
• Do not attempt to open the battery. It contains no
user-serviceable parts.
Failure to observe these precautions may result in
injury or property damage.
• Do not use this tool for continuous use. After 30 to
40 cycles, allow the tool to cool for 15 minutes.
• Do not secure this tool in a vise. This tool is
designed for hand-held operation.
• This tool may be used in damp or wet environments; however, air-drying is recommended before
use if the tool becomes soaked. Damage may
result when the tool is operated prior to thorough
drying when electrical components are soaked.
• Use this tool for the manufacturer’s intended
purpose only.
Failure to observe these precautions may result in
injury or property damage.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
Do not perform any service or maintenance other
than as described in this manual. Injury or damage
to the tool may result.
Failure to observe this precaution may result in injury
and property damage.
Note: Keep all decals clean and legible, and replace
when necessary.
4
Page 5
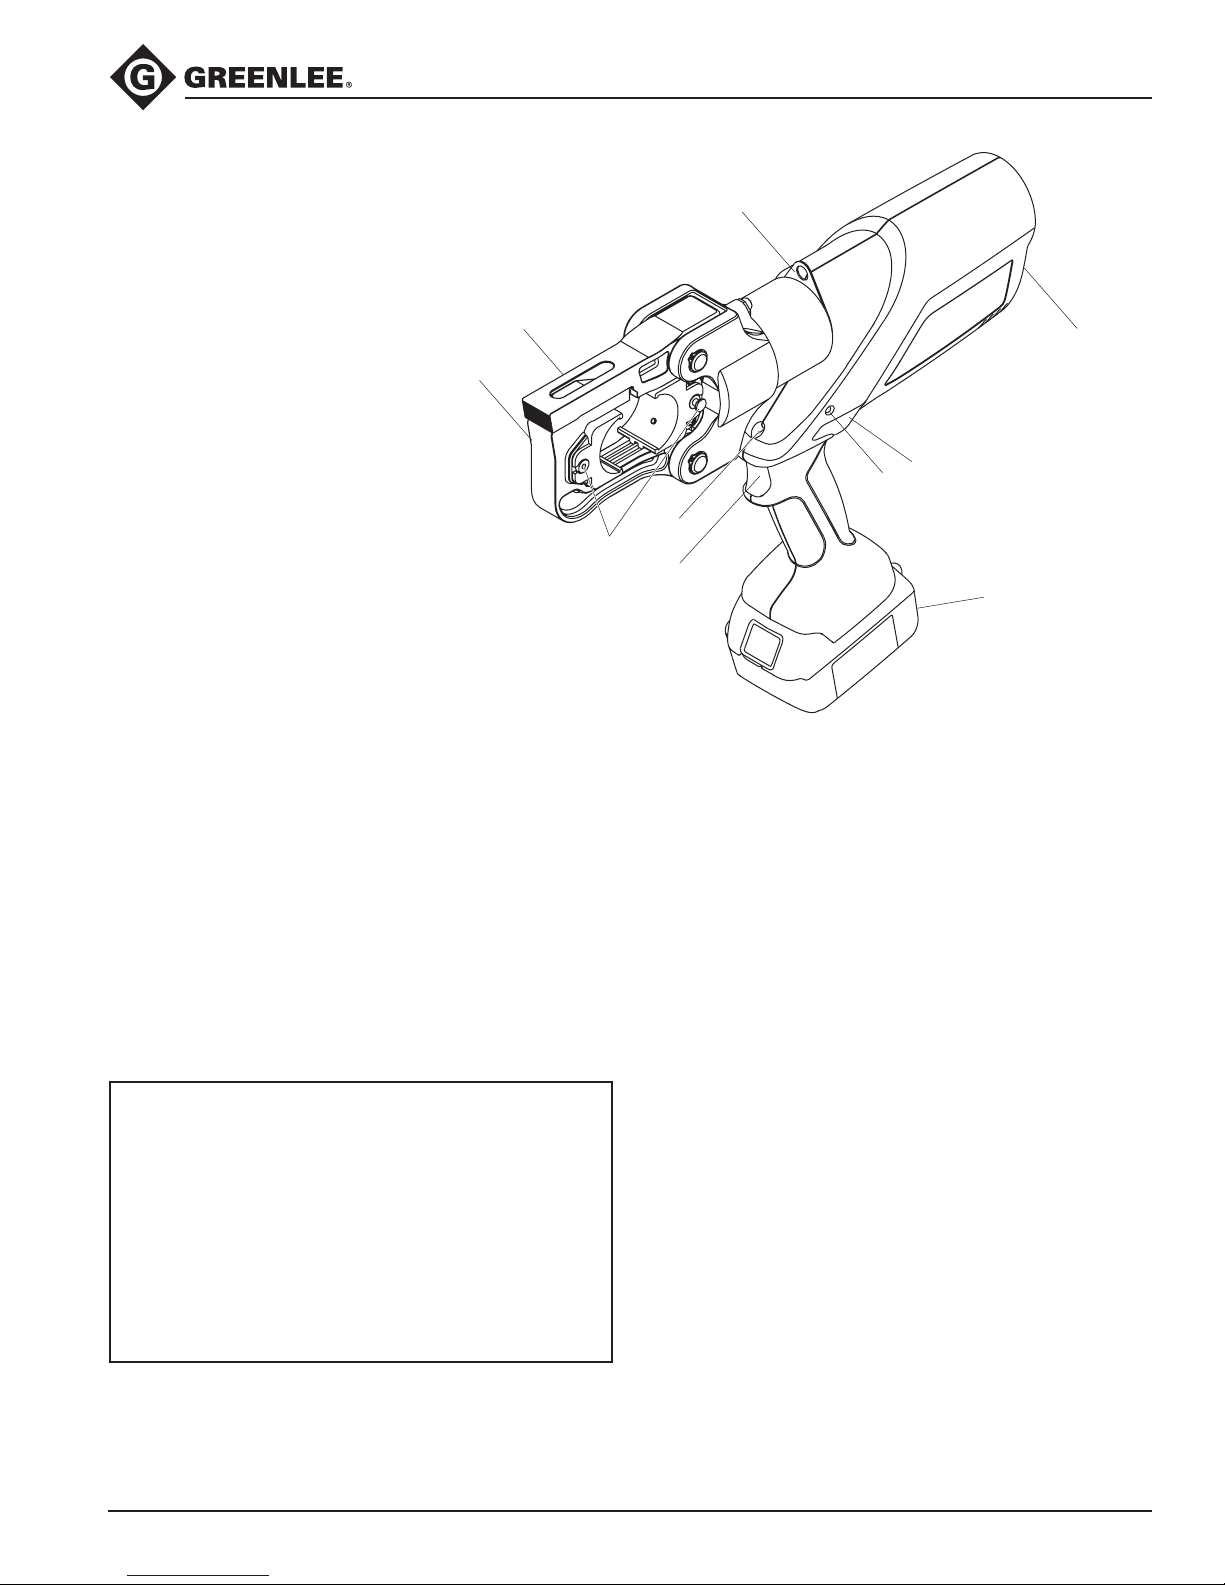
Identification
1. LED Work Light (white)
2. Adapter Release Buttons
3. Head
4. Latch (for opening head)
5. Lanyard Ring
6. Housing
7. Retract Button
8. LED Indicator (red)
9. Battery
10. Trigger
E12CCXL 12-ton Battery-powered Tool
5
4
6
3
7
8
1
2
10
9
Specifications
Tool
Length .....................................................16.5" (419.1 mm)
Width ......................................................... 2.87" (72.9 mm)
Height (with battery) ................................ 14.5" (368.3 mm)
Weight ............................................................15 lb (6.8 kg)
Crimping Force ....................................... 12 tons (106 kN)
Hydraulic Oil ....... 52057878 biodegradable hydraulic uid
Recommended Operating
Temperature Range ......... 5 °F to 122 °F (–15 °C to 50 °C)
Battery Charger
Read the instructions supplied with the battery charger
52047087 120 VAC corded adapter
52047088 230 VAC corded adapter
52049189 18 V, 3 Ah lithium-ion battery
52049201 120 VAC, 18 V charger
52049202 230 VAC, 18 V charger
52049204 12 VDC, 18 V charger
52054992 Li (18 V) to NiCd, NiMH (12 V)
charger adapter
50122746 Carrying strap
Crimping Capacities
Copper Color-Coded Lugs and Splices ............. 750 kcmil
Aluminum Color-Coded Lugs and Splices ......... 750 kcmil
UA12ID Dieless Die Crimping Range
Copper Color-Coded
Lugs and Splices .............................. 4 AWG–750 kcmil
Aluminum Color-Coded
Lugs and Splices .............................. 6 AWG–600 kcmil
5/8" Service Entrance Connectors ................ 10–1/0 AWG
.840 Service Entrance Connectors ............... 1/0–4/0 AWG
Aluminum Overhead “H” Taps ............... 6 AWG–500 kcmil
One-Piece ACSR
Tension Splices ...................................4 AWG–556.5 kcmil
Two-Piece ACSR
Tension Splices ...................................2 AWG–556.5 kcmil
Cutting Capacities
Copper and Aluminum Cable .................... 1-1/2" (40 mm)
ACSR ...................................................954 kcmil (Cardinal)
Standard Guy Strand ................................................... 5/8"
EHS Guy Strand ...........................................................1/2"
Ground Rod ...................................................1/2" (13 mm)
Rebar (schedule 60) .......................................1/2" (13 mm)
Threaded Rod ............................................ 1/4", 3/8", 1/2"
Punching Capacities
Round .....................5-5/8" (144.1 mm) in 10 ga. mild steel
Rectangular .......... 2.677" x 5.433" (68.0 mm x 138.0 mm)
Square ................5.433" x 5.433" (138.0 mm x 138.0 mm)
Accessories required to punch ø 4" through ø 5-5/8":
12185 spacer, 04686 bushing, and 03170 sleeve
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
5
Page 6
Operation
E12CCXL 12-ton Battery-powered Tool
• Inspect tool and dies before use. Replace any
worn or damaged parts. A damaged or improperly assembled tool can break and strike nearby
personnel.
• Carrying strap is for carrying only, not to be used
to hang or suspend tool.
Failure to observe these warnings could result in
severe injury or death.
Electric shock hazard:
This tool is not insulated. When
using this unit on or near energized
electrical lines, use proper personal
protective equipment.
Failure to observe this warning
could result in severe injury or death.
Wear eye protection when operating
or servicing this tool.
Failure to wear eye protection could
result in serious eye injury from
ying debris or hydraulic oil.
Pinch points:
• Remove battery before changing
dies, adapters, or jaws.
• Keep hands away from the crimping tool head when crimping.
Failure to observe these warnings
could result in severe injury or death.
• Do not use this tool for continuous use. After 30 to
40 cycles, allow the tool to cool for 15 minutes.
• Do not secure this tool in a vise. This tool is
designed for hand-held operation.
• This tool may be used in damp or wet environments; however, air-drying is recommended before
use if the tool becomes soaked. Damage may
result when the tool is operated prior to thorough
drying when electrical components are soaked.
• Use this tool for the manufacturer’s intended
purpose only.
Failure to observe these precautions may result in
injury or property damage.
Charging the Battery
Read the instructions supplied with the battery charger.
LED Work Light (white)
This LED automatically turns on when the trigger is
pulled. It remains on for 10 seconds after the trigger is
released.
LED Indicator (red)
This tool is equipped with a special circuit board incorporating several important features to inform the user
about the current status of the unit. The LED signals in
the following cases:
What happens Signal What it means
Flashing light for 2seconds Battery is inserted in tool
Constant light for 20seconds
at end of cycle
Tool will not start, and
constant light for 20seconds
when trigger is released
Tool will stop, and constant
light for 20seconds after
trigger is released
Tool will stop, and flashing
light for 20seconds when
trigger is released
Battery charge is below
17V at beginning of cycle
Battery charge is below
16V at beginning of cycle
Battery voltage drops
below 13V during cycle
Motor current exceeds
20A during cycle
Circuit has become too hot
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
6
Page 7
E12CCXL 12-ton Battery-powered Tool
Operation —Crimping Using KC12 or KA12 type U-style Dies
Setup
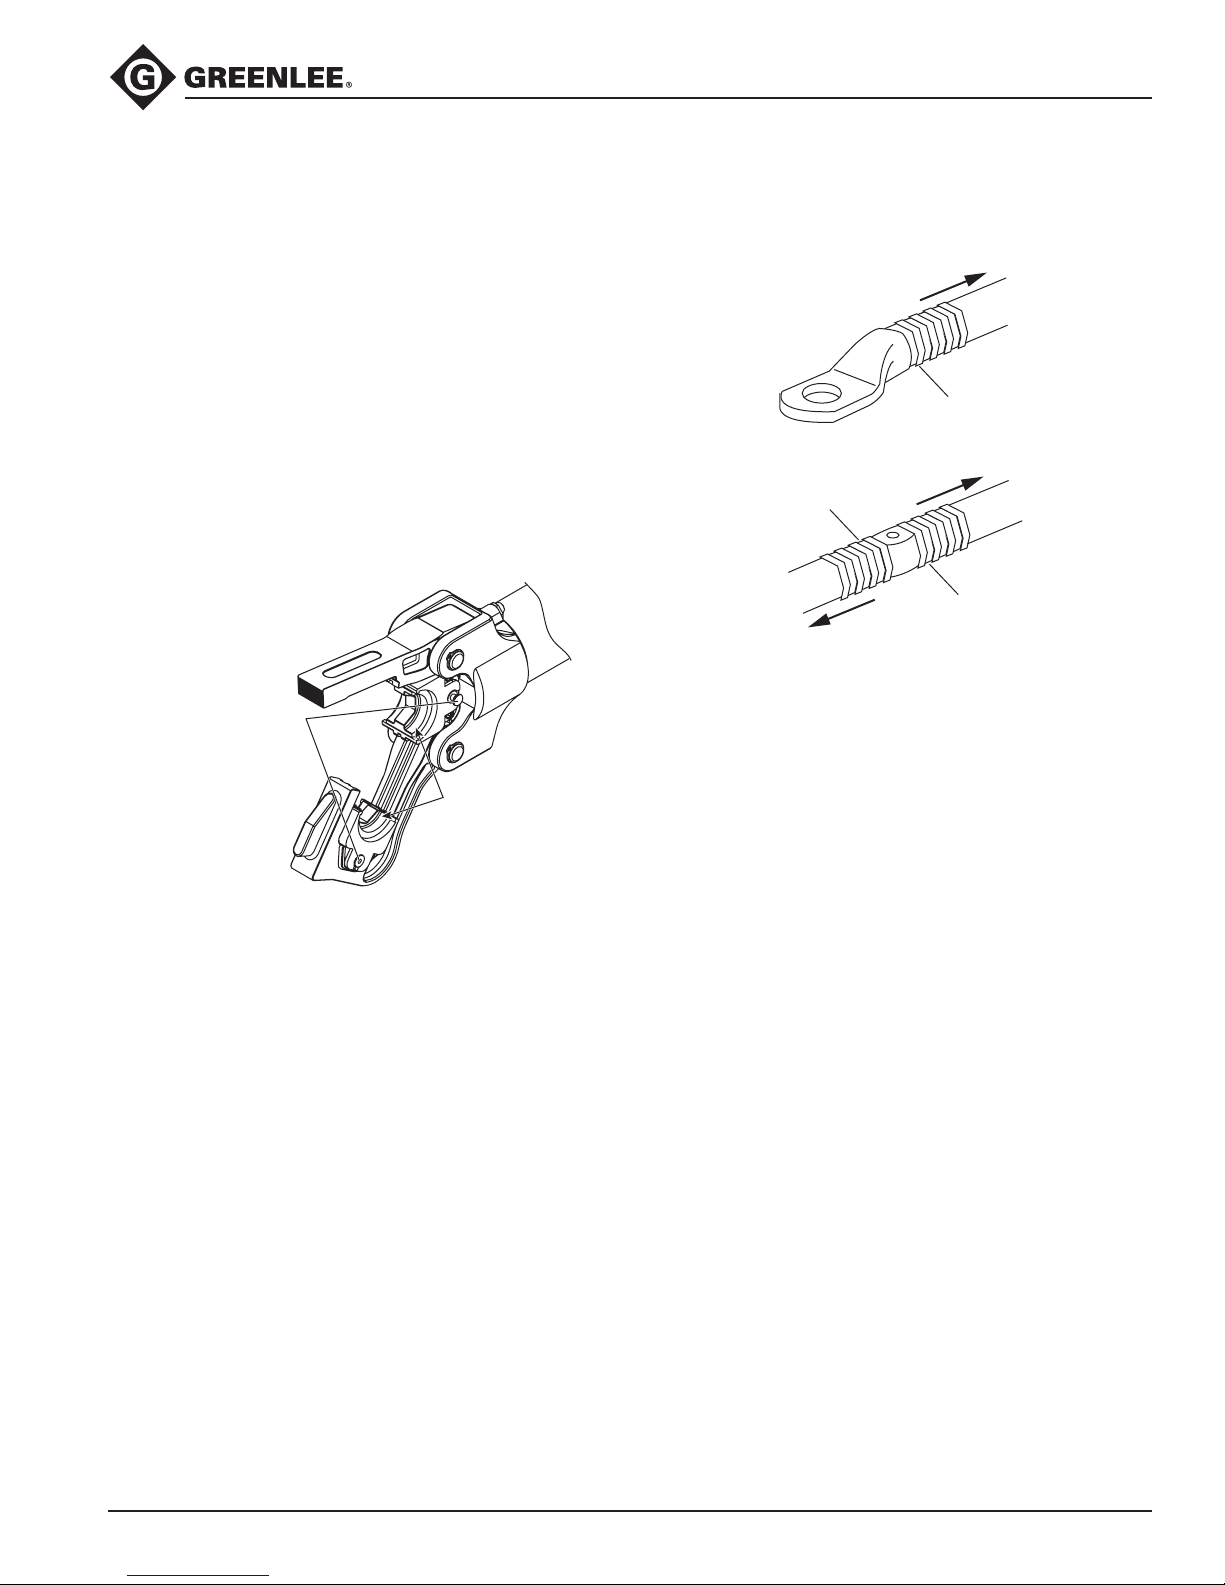
1. Open the tool head.
2. Remove any accessories from the tool head.
3. Select the appropriate set of die adapters and dies.
4. Install the UA12T adapters and U-style dies—one
set in each groove. Lock the die adapters in place
with the detents.
Important: Die adapters must be locked into place
or the die detents will be damaged.
5. Visually check the dies to ensure that they are
aligned correctly so that they will complete the
crimping operation.
6. Close the tool head.
Press detents and slide
UA12T adapters into place
as shown. Release to lock.
Preparing the Cable
Follow the lug manufacturer’s instructions for appropriate cable strip length.
CRIMPING DIRECTION
1ST COMPRESSION
CRIMPING DIRECTION
SIDE B
1ST COMPRESSION
SIDE A
1ST COMPRESSION
CRIMPING DIRECTION
SIDE A
SIDE B
Slide U-style dies
into adapters until
dies snap into place.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
7
Page 8
E12CCXL 12-ton Battery-powered Tool
Operation —Crimping Using KC12 or KA12 type U-style Dies (cont’d)
Crimping Procedure
Wear eye protection when operating
or servicing this tool.
Failure to wear eye protection could
result in serious eye injury from
ying debris or hydraulic oil.
An incomplete crimp can cause a re.
• Use proper die, connector, and cable combinations. Improper combinations can result in an
incomplete crimp.
• The relief valve sounds and the ram automatically
retracts to indicate a completed crimp. If you do
not hear the sound of the relieve valve or the ram
does not automatically retract, the crimp is not
complete.
Failure to observe these warnings could result in
severe injury or death.
1. Press the latch and open the tool head.
2. Insert the properly assembled connector into the
tool head.
3. Close the tool head.
4. Pull the trigger to make the crimp.
5. Hold the trigger down until the crimper achieves
pressure relief.
Notes: Pressure relief occurs at approximately
106 kN bar (12 tons). If you do not hear a “pop,”
the crimp is incomplete.
It is normal for the battery load display to light at
both the beginning and near the end of the crimping
cycle.
6. The ram returns automatically.
7. To stop the ram from returning fully, activate the
trigger for a brief moment. This activation will close
the retraction valve and stop the retraction motion.
8. Position the crimper for the next crimp. Repeat
Steps 4 through 6 for the number of crimps as
described in this manual.
9. Open the crimping head and remove the connector.
Notes: If it is necessary to retract the ram before a
crimp cycle is completed, push the retract button.
Pushing the retract button will result in complete retraction of the ram.
After completing the last crimp on an aluminum
connector, wipe off the excess oxide inhibitor.
Retraction Stop
1. To stop the ram from returning fully, activate the
trigger for a brief moment. This activation will close
the retraction valve, stop the retraction motion, and
set the semi-automatic retraction stop position.
2. Depress the trigger to advance the ram. Hold the
trigger down until the ram automatically retracts.
The ram will partially retract to the set position and
allow the tool to be repositioned.
3. If full retraction is desired, release the trigger at the
end of the crimp.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
8
Page 9
E12CCXL 12-ton Battery-powered Tool
Operation—Crimping Using UA12ID Dieless Die Set
Setup
1. Open the tool head.
2. Remove any accessories from the tool head.
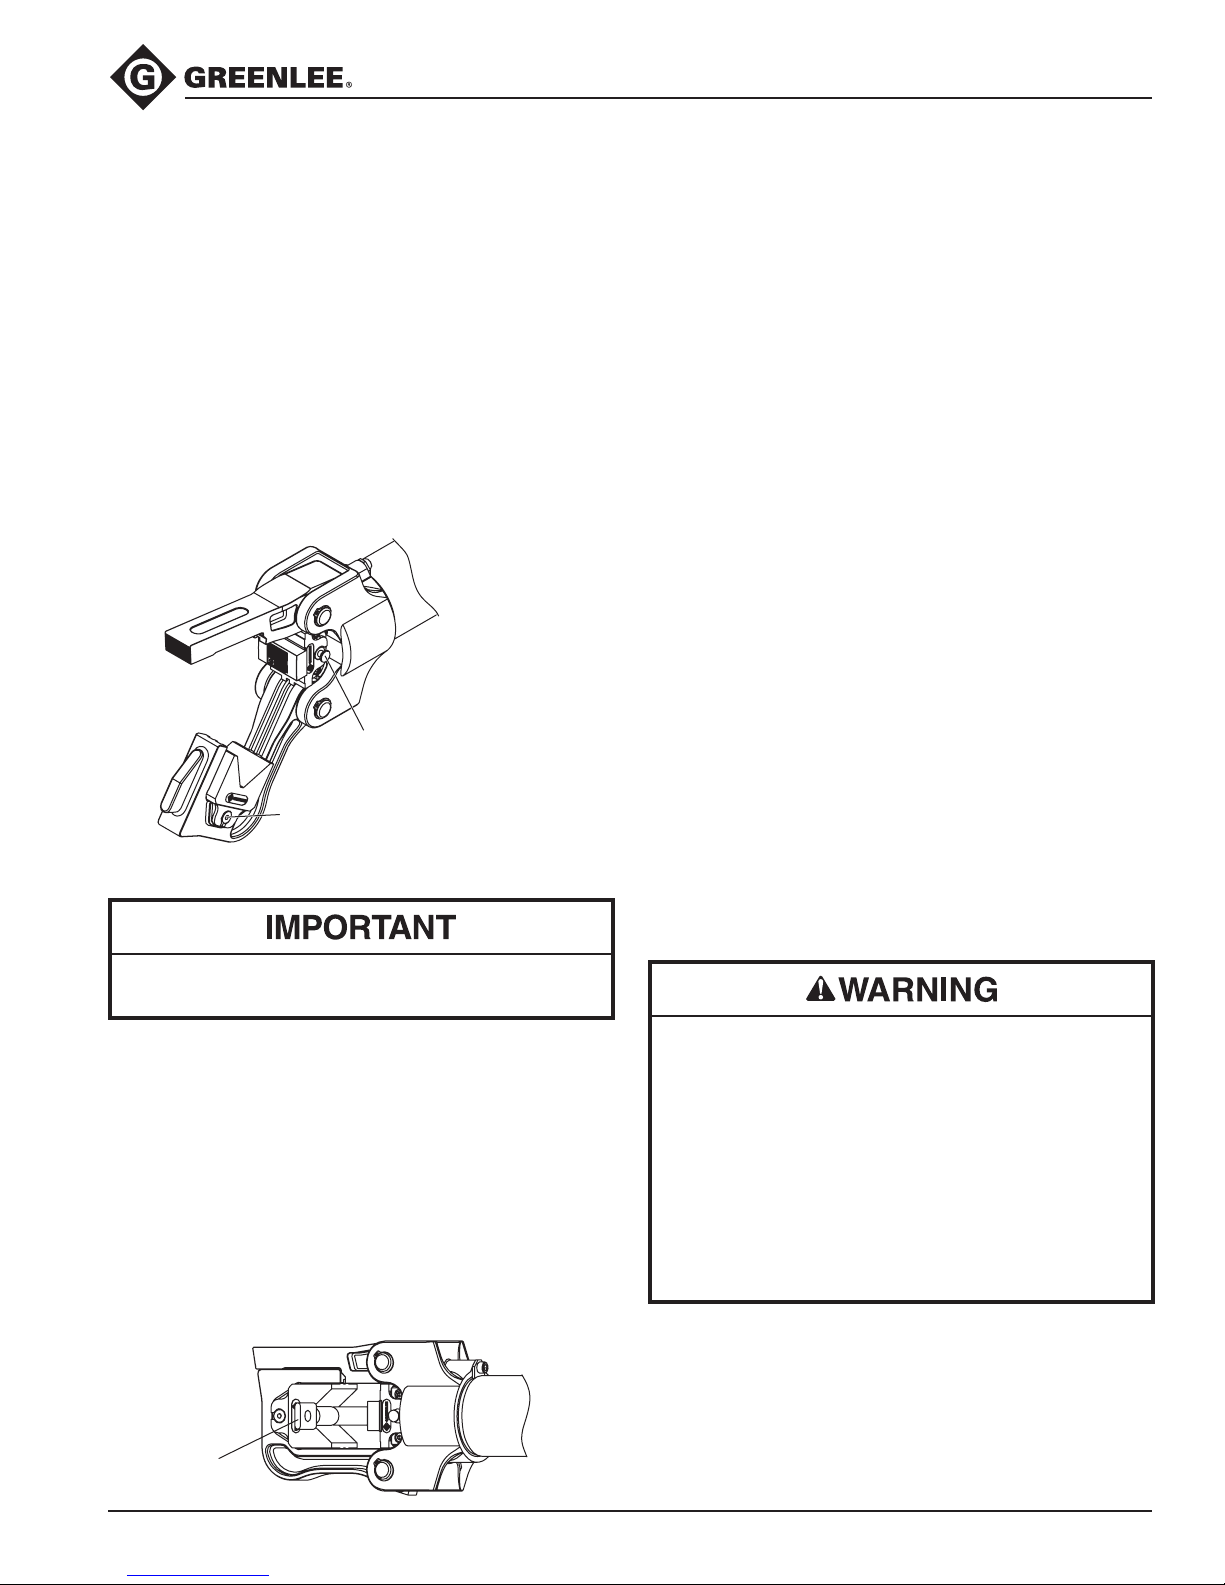
3. Install the UA12ID indenter against the ram and lock
in place with the detent.
4. Install the UA12ID anvil into the head and lock in
place with the detent.
Important: The indenter and anvil must be locked
into place or the detents will be damaged.
5. Visually check the indenter and anvil to ensure that
they are aligned correctly so that they will complete
the crimping operation.
6. Close the tool head.
Press detent and slide
UA12ID indenter into place
as shown. Release to lock.
Press detent and slide UA12ID anvil
into place as shown. Release to lock.
Preparation
3. If open, close the crimping head. Make sure the
head and latch are fully engaged.
4. For a cUL or UL classied crimp, complete the
number of crimps specied under “Connector
Table” in this manual.
5. For a single crimp, position the connector so the
crimp will be located at the center of the barrel.
For a double crimp, position the connector so two
crimps will be evenly spaced between the connector marks.
6. Depress the trigger to advance the indenter. Hold
the trigger down until the indenter automatically
begins to retract.
Notes: If the crimping tool does not automatically
retract, the crimp is incomplete.
It is normal for the battery load display to light at
both the beginning and near the end of the crimping
cycle.
7. Release the trigger until the indenter retracts
completely.
8. To stop the ram from returning fully, activate the
trigger for a brief moment. This activation will close
the retraction valve and stop the retraction motion.
9. Lift the latch to open the crimping head and remove
the connector.
Note: If it is necessary to retract the indenter before
a crimp cycle is complete, push the retract button.
Pushing the retract button will result in complete
retraction of the indenter.
After completing the last crimp on an aluminum
connector, wipe off the excess oxide inhibitor.
For a cUL or UL classied crimp, refer to “Connector
Table” in this instruction manual.
1. Select a proper size and type of connector to
correspond with the wire or cable.
2. Strip the cable to an appropriate length. Follow the
connector manufacturer’s instructions.
Note: Apply an oxide inhibitor, if required.
Refer to the connector manufacturer’s instructions.
3. Clean the die seat area.
Crimping Procedure
1. Insert the cable fully into the connector.
An incomplete crimp can cause a re.
• Use proper die, connector, and cable combinations. Improper combinations can result in an
incomplete crimp.
• The relief valve sounds and the ram automatically
retracts to indicate a completed crimp. If you do
not hear the sound of the relieve valve or the ram
does not automatically retract, the crimp is not
complete.
Failure to observe these warnings could result in
severe injury or death.
2. Place the connector into the V of the crimping head
as shown below.
Automatic Retraction Stop
1. Depress the trigger to advance the indenter. Hold
the trigger down until the indenter automatically
retracts. The indenter will partially retract to allow
the tool to be repositioned.
Connector
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
2. If full retraction is desired, release the trigger at the
end of the crimp.
9
Page 10
Operation —Cutting
Electric shock hazard:
This tool is not insulated. When
using this unit on or near energized
electrical lines, use proper personal
protective equipment.
Failure to observe this warning
could result in severe injury or death.
Wear eye protection when operating
or servicing this tool.
Failure to wear eye protection could
result in serious eye injury from
ying debris or hydraulic oil.
E12CCXL 12-ton Battery-powered Tool
Accessory Table
Task Blade
Copper and aluminum
26 mm (1.00") max.
Copper and aluminum
40 mm (1.56") max.
ACSR
Copperweld
ACAR
Guy strand
EHS guy strand
Ground rod
Anchor rod
Soft bolts
Rebar
Threaded rod Threaded rod
UC26
UC40
UCACSR
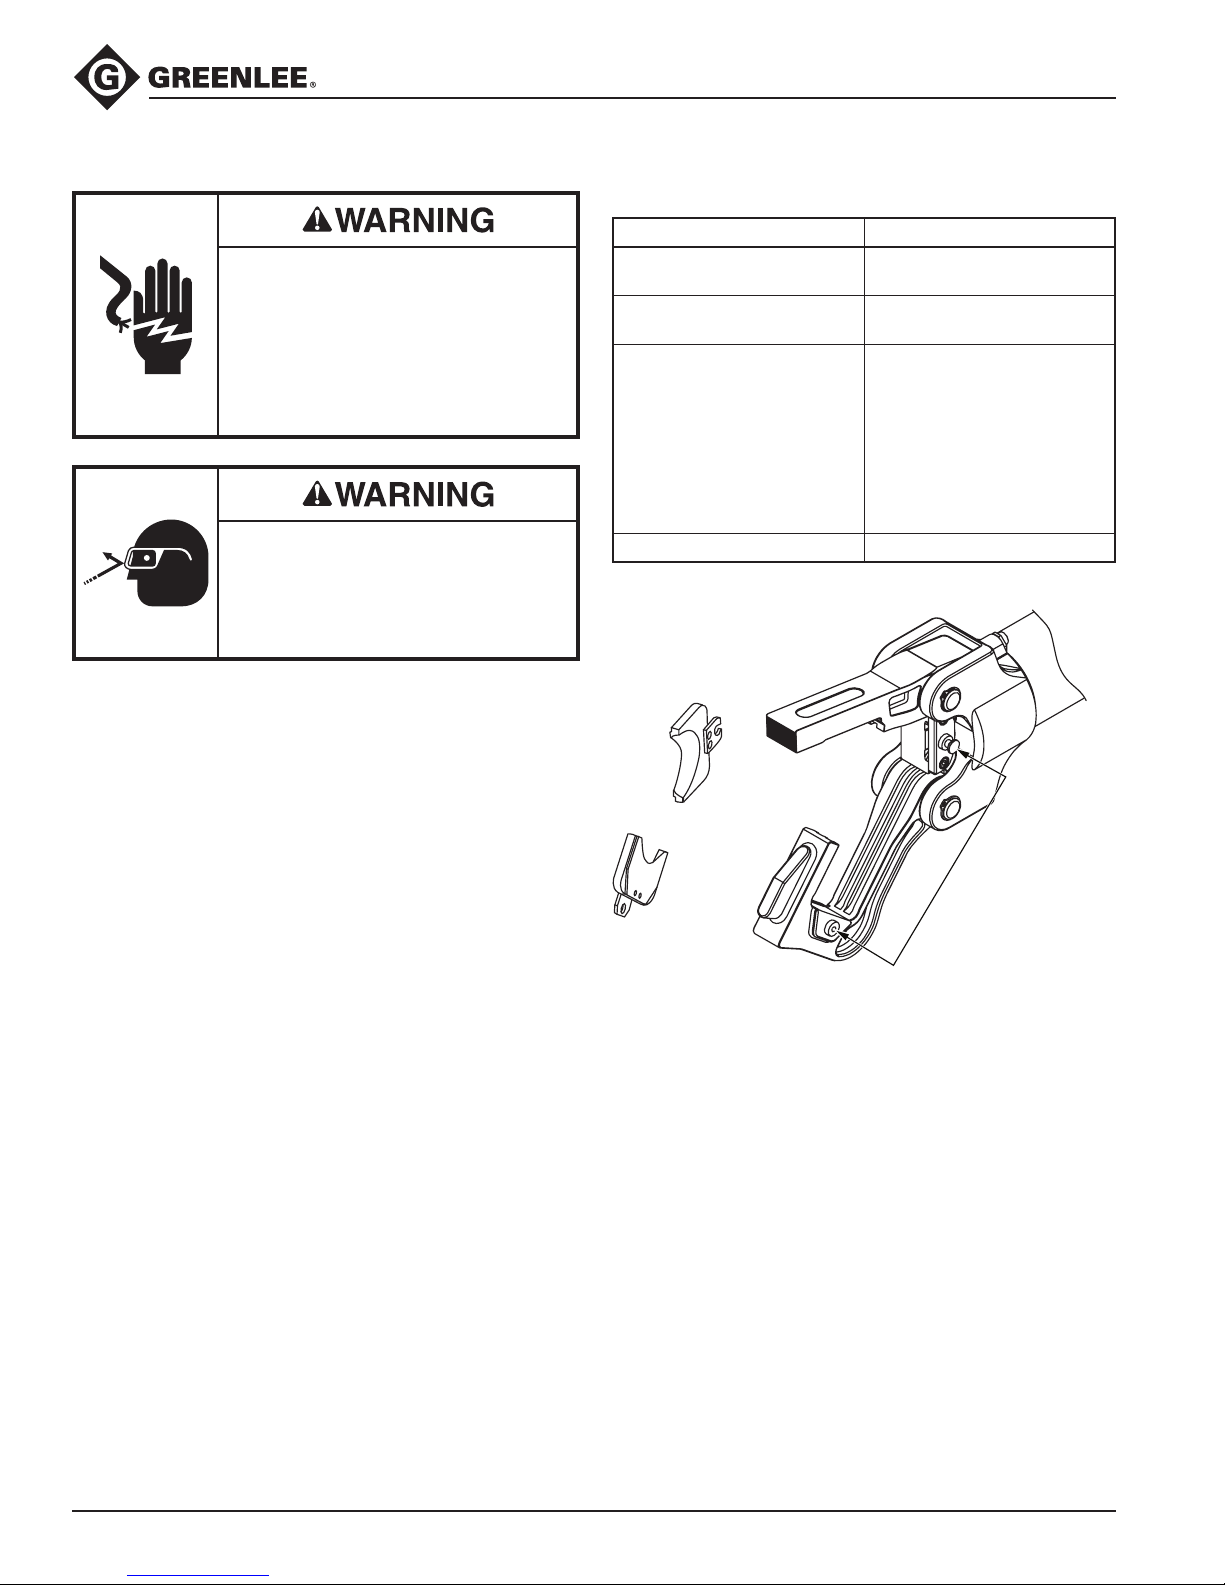
Setup
1. Open the tool head.
2. Remove any accessories from the tool head.
3. Select the appropriate set of blades, using the
table provided on this page.
4. Install one blade in each groove. Slide the tab into
the slots in the ram and head. Lock them in place
with the W-type detents.
5. Visually check the blades to ensure that they are
aligned correctly so that they will complete the
butting operation.
6. Close the tool head.
Detents:
Press and slide the
adapter and/or die
into place.
Release to lock.
Cutting Procedure
1. Press the latch and open the tool head.
2. Position the item to be cut in the tool head.
3. Close the tool head.
4. Pull the trigger to cut the item.
5. Release the trigger when the cut is complete.
6. The ram returns automatically.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
10
Page 11
Operation—Punching
E12CCXL 12-ton Battery-powered Tool
Electric shock hazard:
Do not use this tool as a punch driver
on or near live circuits. This includes,
but is not limited to, the following
circumstances:
• Energized electrical lines
• Energized circuit breaker panels
and fuse boxes
• Junction boxes with energized
circuits
Failure to observe this warning could
result in severe injury or death.
Wear eye protection when operating
or servicing this tool.
Failure to wear eye protection could
result in serious eye injury from
ying debris or hydraulic oil.
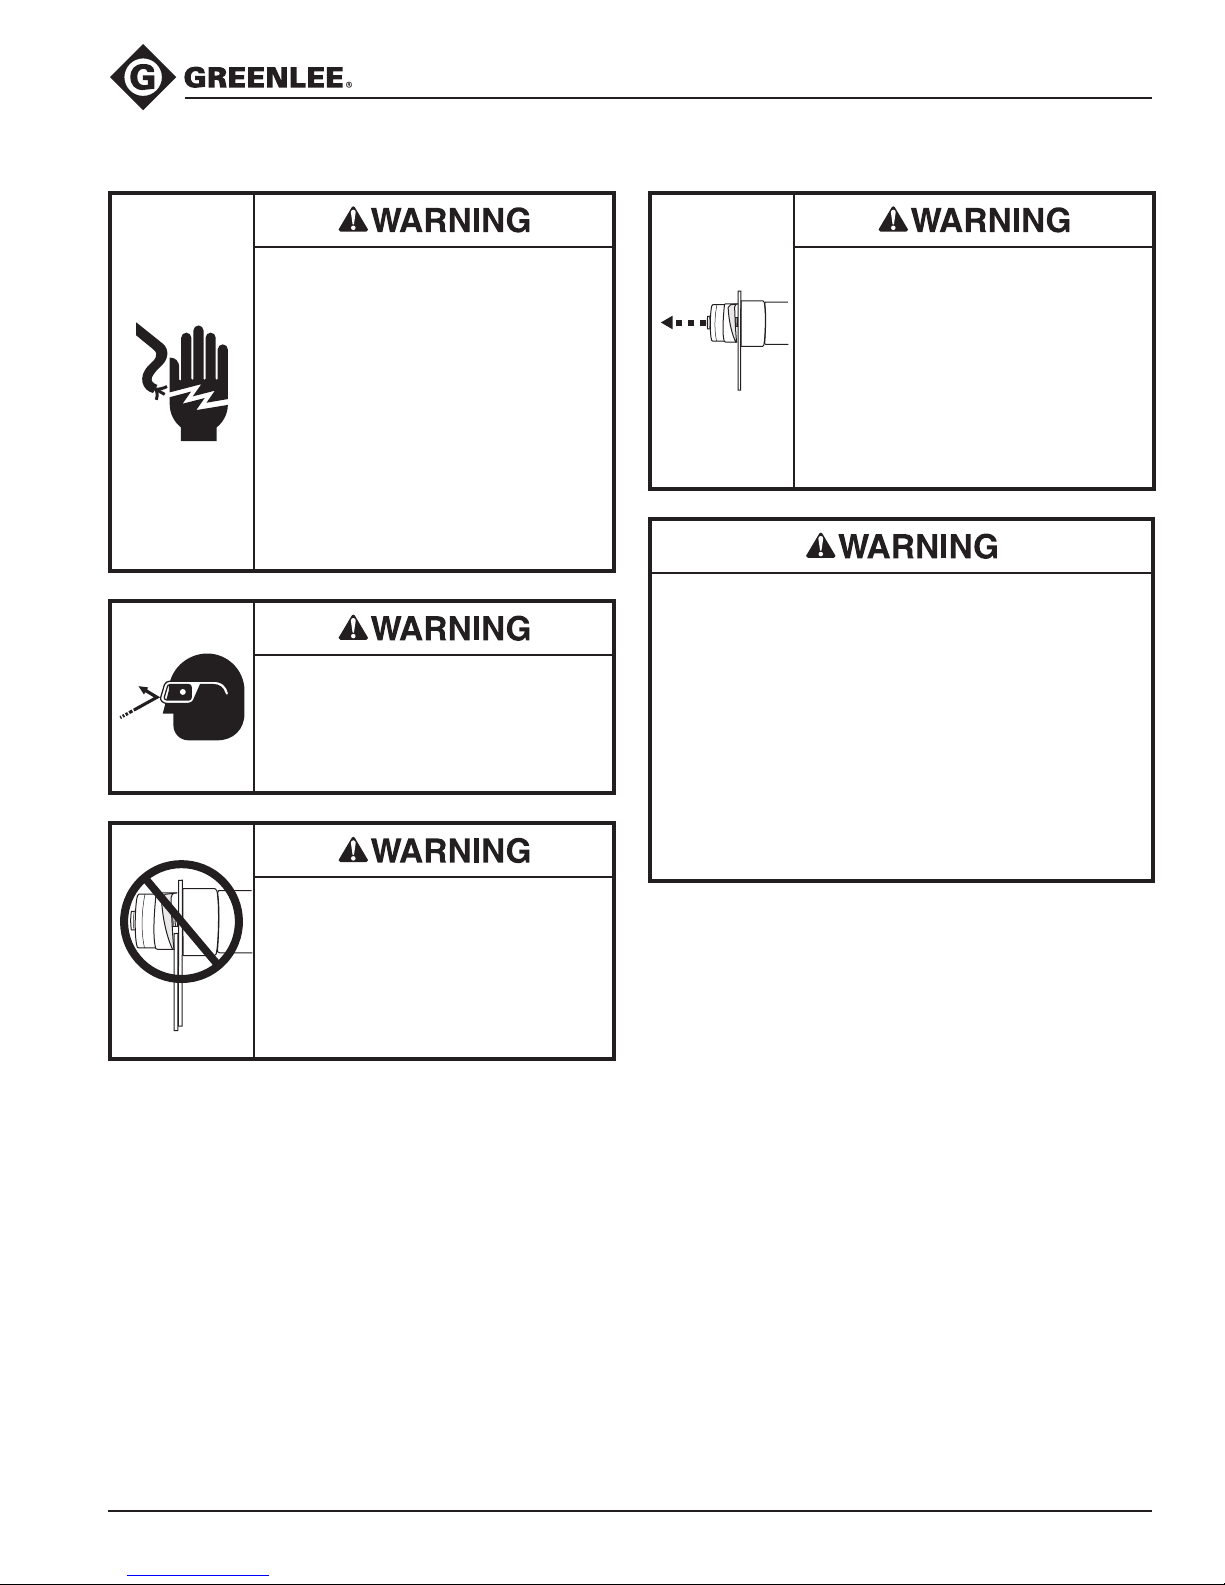
A component failure could throw
broken parts.
• Do not allow anyone to stand in
front of the punch.
• Close access doors or covers on
any equipment that is in line with
the punch.
Failure to observe this warning could
result in severe injury or death.
Set up the tool properly. An improper setup could
cause a component to fail and strike nearby
personnel with great force.
• Thread the punch completely onto the draw stud.
All of the punch threads must be engaged by the
draw stud threads. Incomplete assembly could
cause a component failure.
• Use only Greenlee punches, dies, and draw studs.
Other manufacturers’ components might not withstand the forces generated by this punch driver.
Failure to observe these warnings could result in
severe injury or death.
Do not attempt to punch a hole
through two or more thicknesses of
material. This will bend or break the
draw stud, and could throw parts with
great force.
Failure to observe this warning could
result in severe injury or death.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
11
Page 12
Operation—Punching (cont’d)
E12CCXL 12-ton Battery-powered Tool
Setup and Punching Procedure
1. Open the tool head.
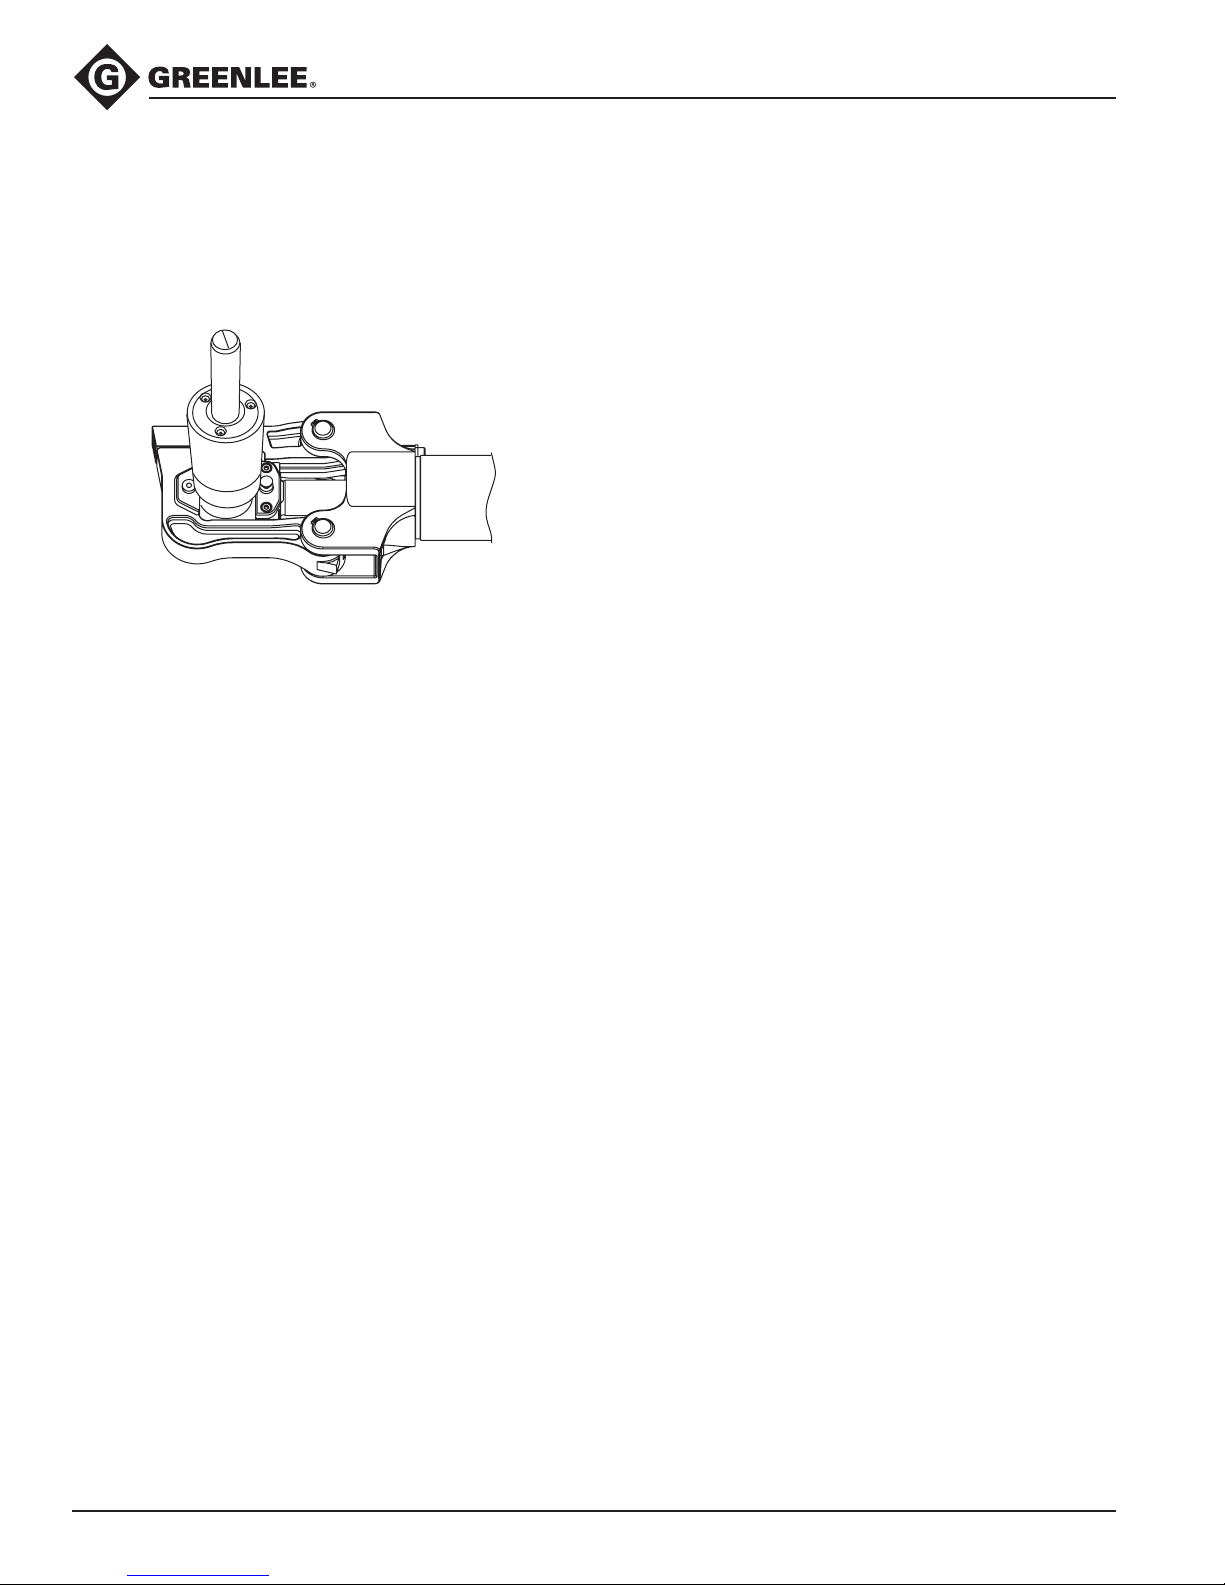
2. Remove any accessories from the tool head.
3. Install the punch driver so that the drive piston is
toward the yoke, as shown.
4. Close the tool head.
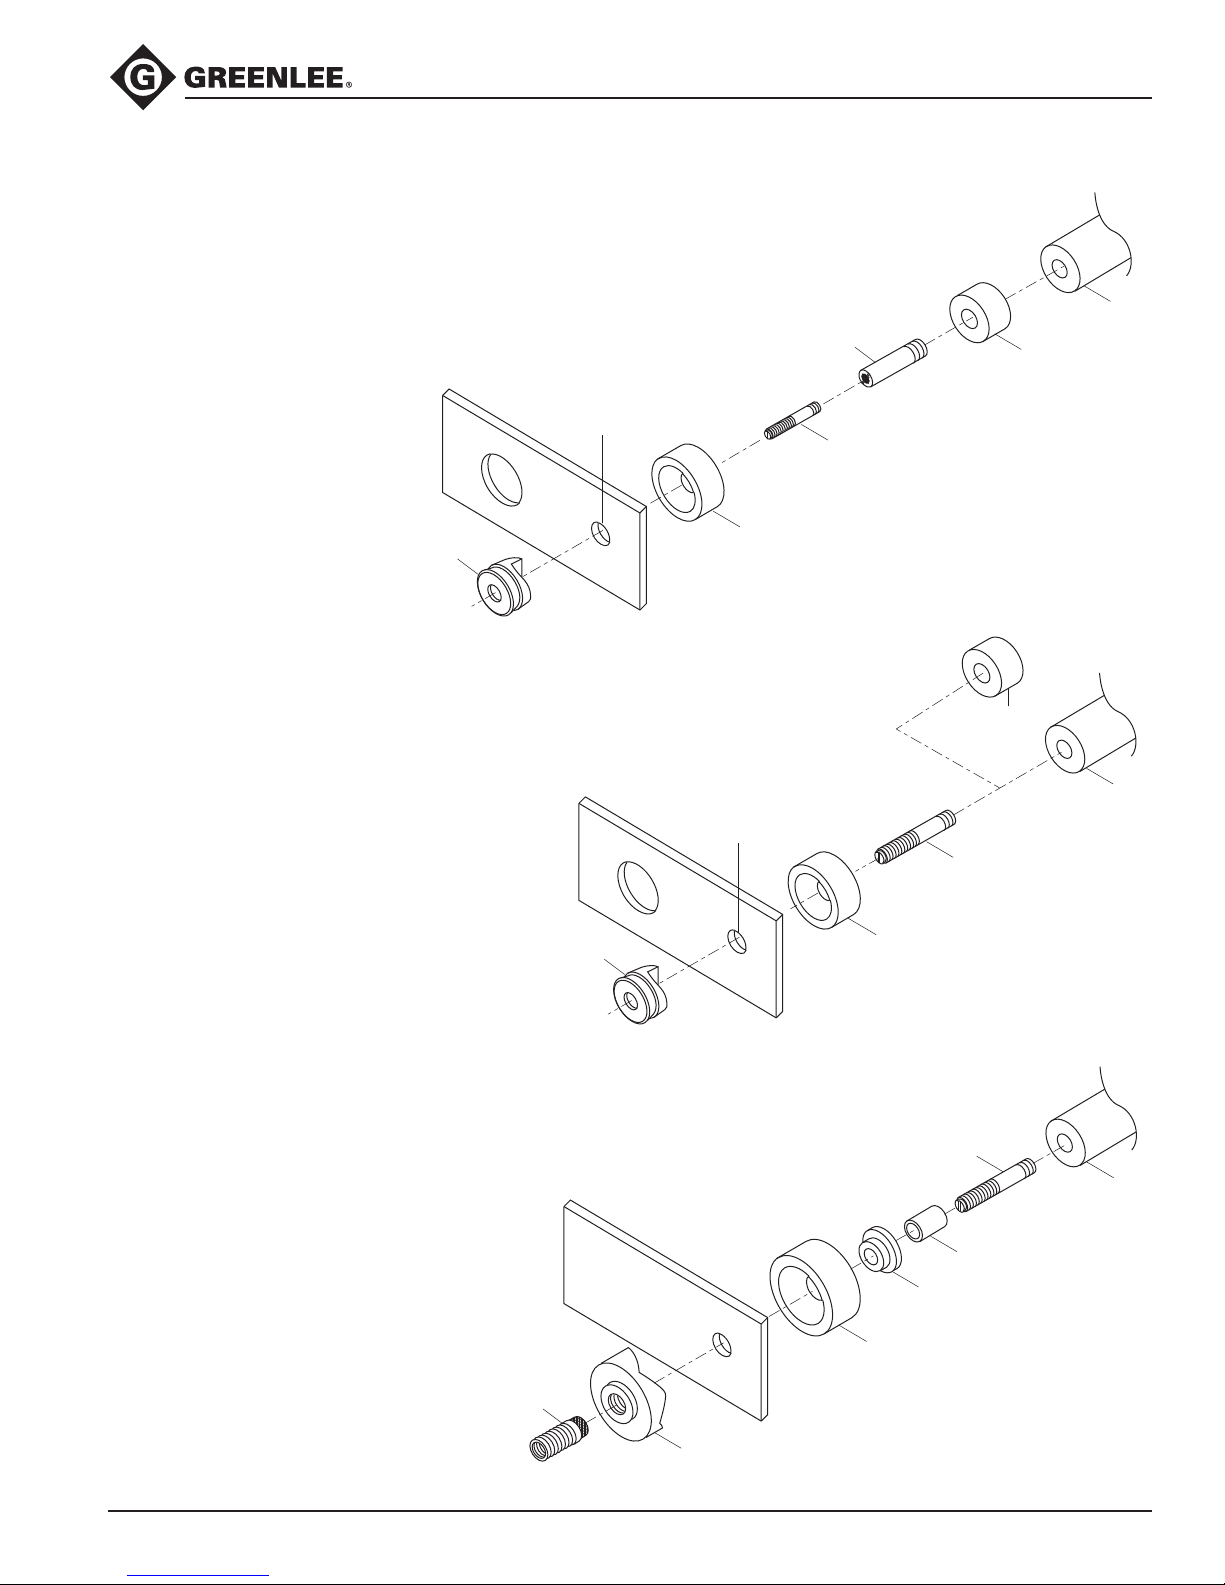
5. Select the punch, die, and draw stud to make the
appropriate size hole. Refer to the illustrations on
the following pages.
6. Determine and mark the exact location for the hole.
Use a Greenlee Kwik Stepper® drill bit to drill a hole
that is slightly larger than the draw stud. This is the
pilot hole.
7. Push the retract button and hold the button until the
ram is completely retracted.
8. Thread the 3/4" draw stud or 3/4" adapter completely into the punch driver. Refer to the illustrations on the following pages.
Notes: For a punch and die with a 3/8" center hole,
thread the 3/8" draw stud into the end of the 3/4"
adapter.
For 4" and larger punch and die, add the bushing
to the die, slide the spacer over the 3/4" draw stud,
and install the 1-1/8" sleeve.
9. Install a spacer, if necessary. Refer to the illustrations on the following pages.
10. Slide the die over the draw stud with the open end
of the die facing away from the punch driver.
11. Insert the draw stud through the pilot hole.
12. Thread the punch onto the draw stud with the
cutting surfaces of the punch facing the material.
Tighten the punch by hand until the spacer, die,
material, and punch contact each other.
Note: All of the punch threads must be engaged by
the draw stud threads. If any of the punch threads
are not engaged, disassemble the setup, remove the
spacer, and reassemble the setup.
13. Pull the trigger.
Note: A “popping” sound indicates that the tool
has reached relief pressure. This may indicate that
the attempted operation is beyond the capacity of
the tool.
14. Release the trigger when the punch completes the
hole. The ram returns automatically.
15. Unscrew the punch. Remove slugs from the die.
Remove the spacer and unscrew the draw stud.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
12
Page 13
Operation—Punching (cont’d)
E12CCXL 12-ton Battery-powered Tool
Round Punches
Metric: 22.5 mm (max.)
Conduit Size: 1/2" (max.)
Actual Size: 0.885" (max.)
Round Punches
Metric: 28.3 mm to 95.2 mm
Conduit Size: 3/4" to 3"
Actual Size: 1.115" to 3.75"
Punch
1/2" (12.7 mm)
Pilot Hole
Die
7/8" (22.2 mm)
Pilot Hole
33967
3/4" Adapter
30043
3/8" Draw Stud
Punch
Driver
03248
Spacer
03248
Spacer
Punch
Driver
2113AA or 29452
3/4" Draw Stud
Round Punches
Metric: 95.2 mm to 143 mm
Conduit Size: 3-1/2" to 5"
Actual Size: 4" to 5-5/8"
1557AA
1-1/8" Sleeve
Punch
Die
29452
3/4" Draw Stud
Punch
Driver
12185 Spacer
3037AV Bushing
Die
Punch
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
13
Page 14
Operation—Punching (cont’d)
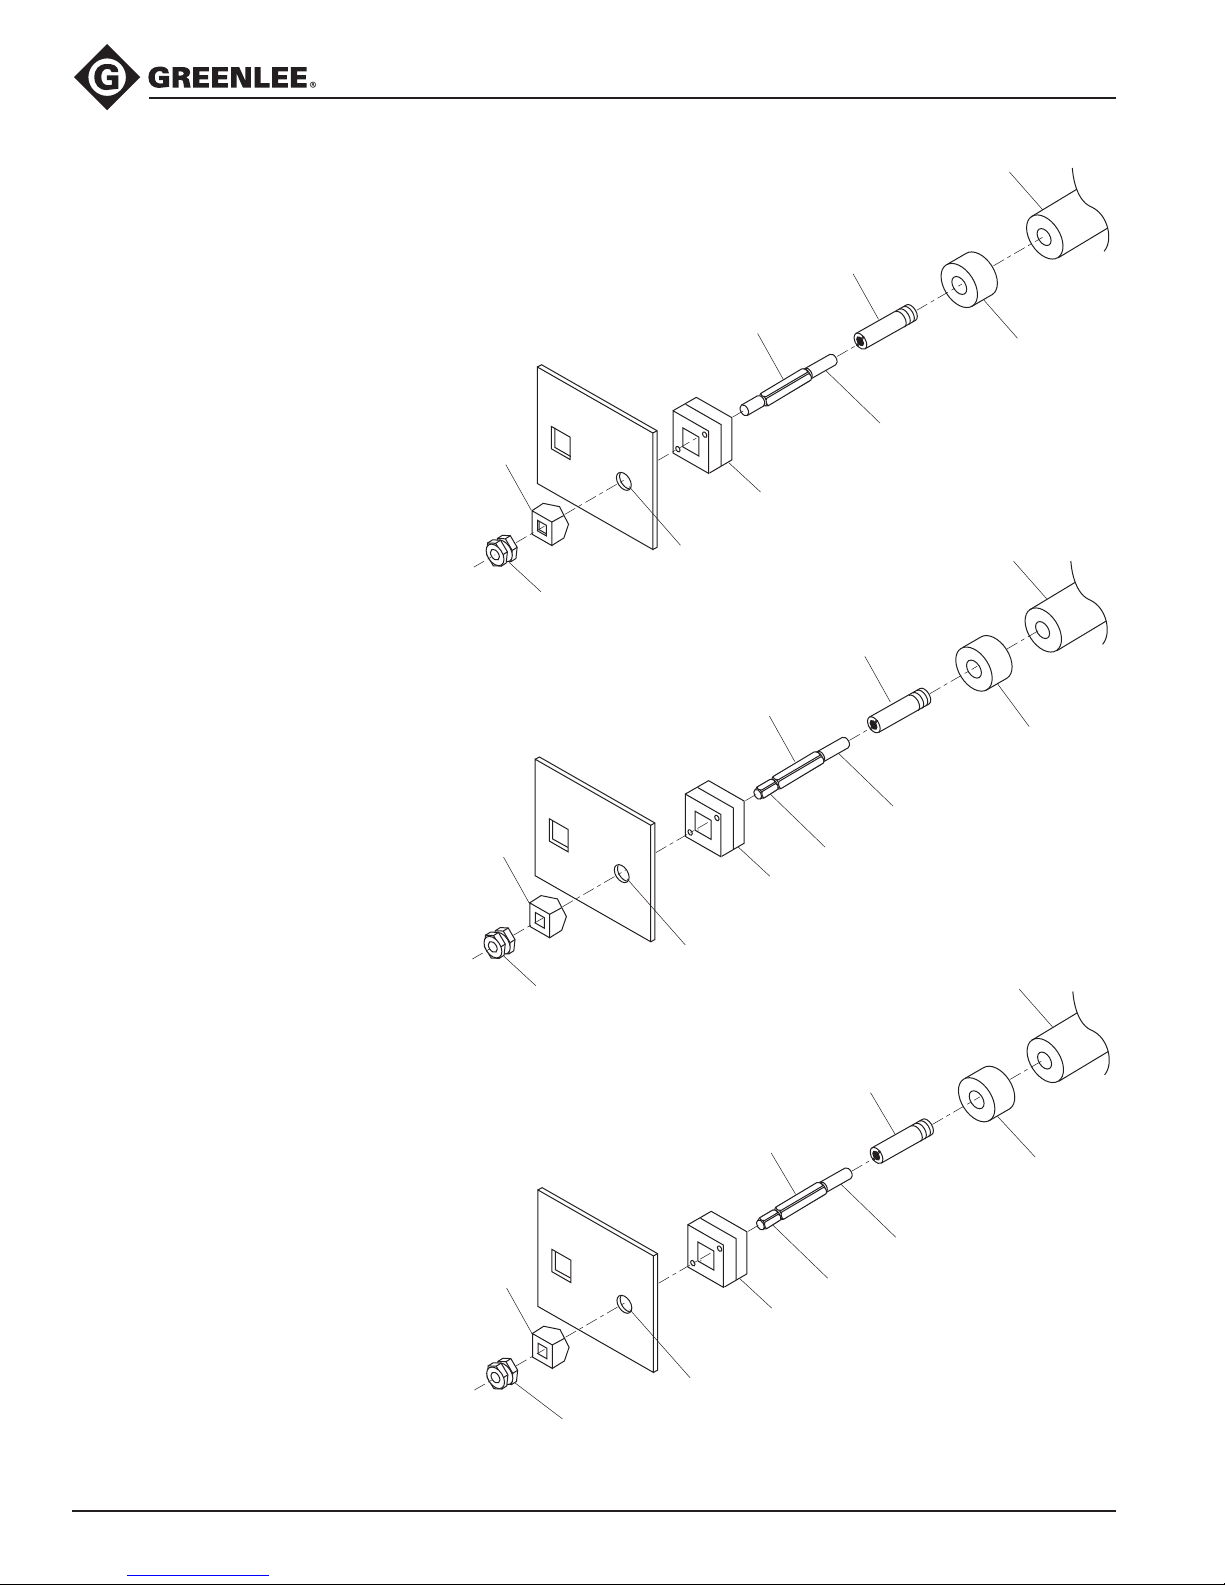
Punch Driver
Square and Rectangular Punches
Metric: 12.7 mm square
Inches: 1/2" square
Metric: 11.1 mm x 22.2 mm rectangular
Inches: 7/16" x 7/8" rectangular
Punch
E12CCXL 12-ton Battery-powered Tool
60114
1/4" Adapter
60115
1/4" Draw Stud
03248
Spacer
End with Long Threads
Die
Square and Rectangular Punches
Metric: 15.9 mm to 24.0 mm square
Inches: 5/8" to 0.945" square
Metric: 17.0 mm x 19.0 mm rectangular
Inches: 0.670" x 0.749" rectangular
Square and Rectangular Punches
Metric: 25.4 mm square
Inches: 1" square
Metric: 19.1 mm x 29.0 mm to
31.8 mm x 35.1 mm rectangular
Inches: 0.750" x 1.140" to
1.250" x 1.380" rectangular
05244
1/4" Counter Nut
Punch
04638
3/8" Counter Nut
Punch
Pilot Hole
Pilot Hole
Punch Driver
33967
3/8" Adapter
60116
3/8" Draw Stud
03248
Spacer
End with Long Threads
Threads with Flats
Die
Punch Driver
60167
1/2" Adapter
60117
3/8" Draw Stud
03248
Spacer
End with Long Threads
Threads with Flats
Die
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
Pilot Hole
60258
1/2" Counter Nut
14
Page 15
E12CCXL 12-ton Battery-powered Tool
Operation—Punching (cont’d)
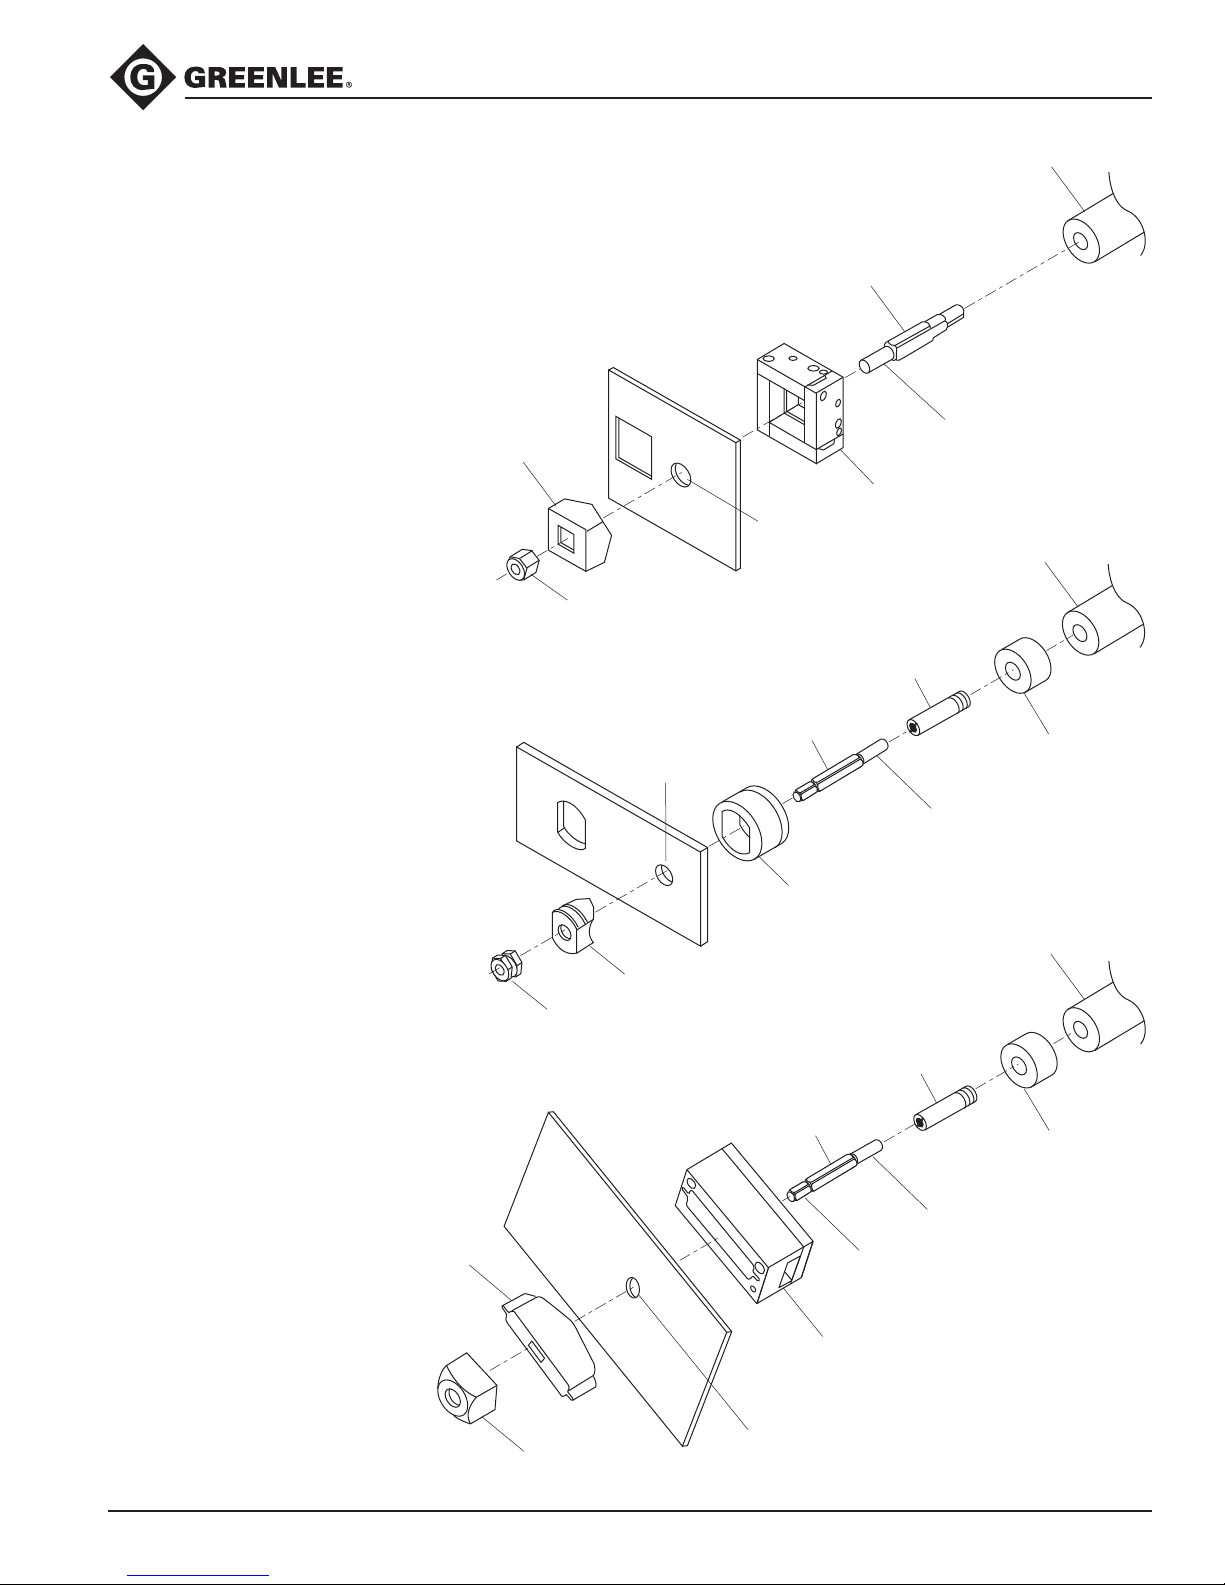
Square and Rectangular Punches
Metric: 46.0 mm to 68.0 square
Inches: 1.811" to 2.677" square
Metric: 33.3 mm x 66.7 mm to
35.0 mm x 65.0 mm rectangular
Inches: 1.312" x 2.625" to
1.378" x 2.559" rectangular
“D”, Double “D”, and
Key Punches
Punch
3/4" Counter Nut
60235
Pilot Hole
Punch Driver
60118
3/4" Draw Stud
End with Long Threads
Die
Pilot Hole
Punch Driver
Adapter
Draw Stud
03248
Spacer
End with Long Threads
Electronic Connector
Panel Punches
Punch
Counter Nut
04638
3/8" Counter Nut
Die
Punch Driver
Punch
33967
3/8" Adapter
34421
3/8" Draw Stud
03248
Spacer
End with Long Threads
Threads with Flats
Die
7/16" (11.1mm)
Pilot Hole
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
15
Page 16
E12CCXL 12-ton Battery-powered Tool
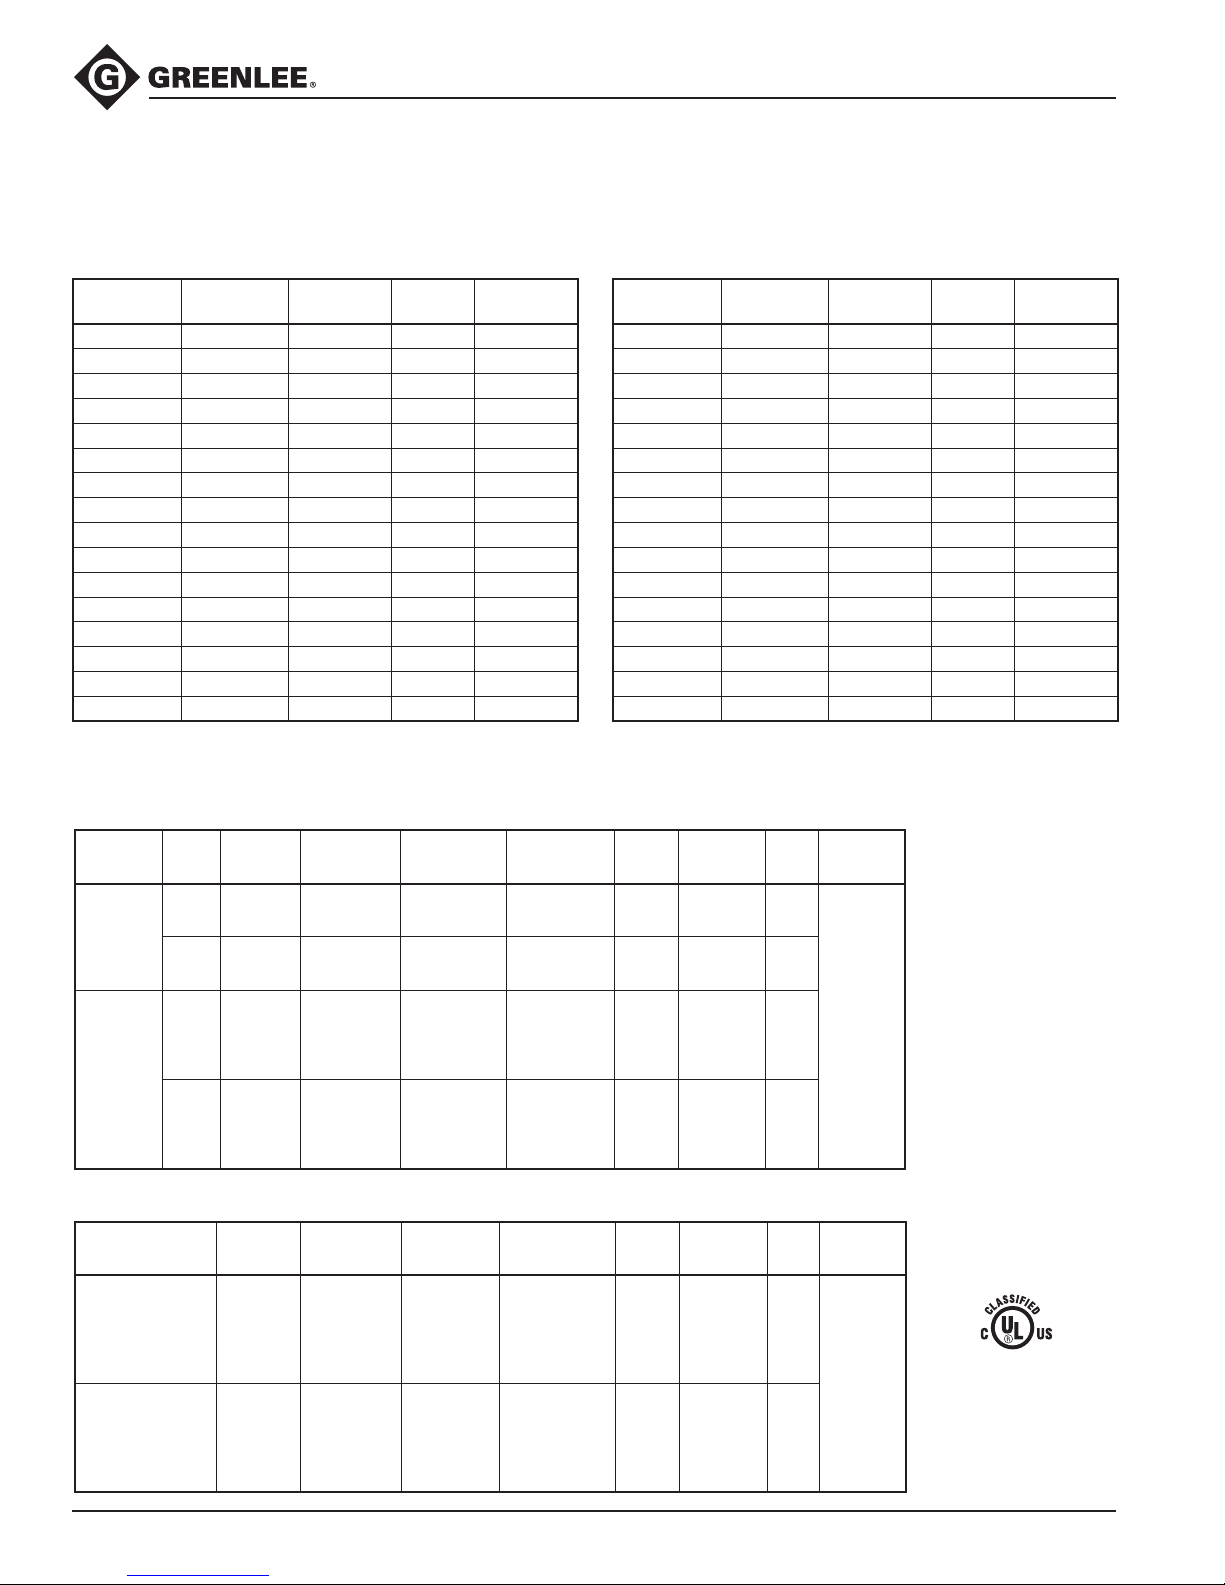
Die Selection
Refer to “Connector Selection” for brand names and model numbers of appropriate lugs as well as crimping instructions.
Crimps made with this tool and KC12-type or KA12-type dies are cUL and UL classied when used with the appropriate conductor
and connectors listed below.
Dies for Copper Connectors
Catalog
No.
KC12-8 10996 8 AWG Red 1
KC12-6 10997 6 AWG Blue 1
KC12-4 10998 4 AWG Gray 1
KC12-2 10999 2 AWG Brown 1
KC12-1 11003 1 AWG Green 1
KC12-1/0 11004 1/0 AWG Pink 1
KC12-2/0 11007 2/0 AWG Black 1
KC12-3/0 11010 3/0 AWG Orange 1
KC12-4/0 11011 4/0 AWG Purple 1
KC12-250 11012 250 kcmil Yellow 1
KC12-300 11013 300 kcmil White 2
KC12-350 11014 350 kcmil Red 2
KC12-400 11015 400 kcmil Blue 2
KC12-500 11016 500 kcmil Brown 2
KC12-600 11018 600 kcmil Green 2
KC12-750 11020 750 kcmil Black 2
UPC
No.
Cable
Size
Color
Code
No. of
Crimps
Dies for Aluminum Connectors
Catalog
No.
KA12-8 22084 8 AWG Blue 1
KA12-6 22085 6 AWG Gray 1
KA12-4 22086 4 AWG Green 1
KA12-2 22087 2 AWG Pink 1
KA12-1 22088 1 AWG Gold 1
KA12-1/0 22089 1/0 AWG Tan 1
KA12-2/0 22090 2/0 AWG Olive 2
KA12-3/0 22121 3/0 AWG Ruby 2
KA12-4/0 22122 4/0 AWG White 2
KA12-250 22123 250 kcmil Red 2
KA12-300 22124 300 kcmil Blue 2
KA12-350 22125 350 kcmil Brown 2
KA12-400 22126 400 kcmil Green 3
KA12-500 22127 500 kcmil Pink 3
KA12-600 22128 600 kcmil Black 3
KA12-750 22129 750 kcmil Yellow 3
UPC
No.
Cable
Size
Color
Code
No. of
Crimps
Connector Selection (NOT for use with flex, navy or welding wire)
Tool Range: 8 AWG to 750 kcmil
When used with KC12-type dies, this tool is cUL and UL classied for use with the following connector brands:
CONNECTOR
TYPE
Copper
Splices
Copper
Lugs
BARREL
TYPE
Short
Long
Short
Long
ANDERSON
VHSS
VHS
VHCS
VHCL
BLACKBURN
CSP
CU
CTL-2/CTL
CTL-L/LCN
®
BURNDY
YS-L
YS
YA-2LN/
YA-L/YA-2L;
YA/YA-L-TC/
YA-L-2TC
YA/YAZ
YA-2N/YA-2TC
YAZ-2N/YAZ-2TC
ILSCO
CT
CTL
CSW
CRA/CRB
CRC
CLN, CLW
CRA-L/CRB-L
CRA-2/CRB-2L
CRC-2L
PANDUIT
SCSS
SCS
SCL
SCH
LCAS
LCA
LCD
LCAN
LCB
LCC
T&B
54504 to
54523-TB
54804 to
54823
54104 to
54123-TB;
54204 to
54223
54930BE to
54923BE;
54850BE to
54880BE
PENNUNION
When used with KA12-type dies, this tool is cUL and UL classied for use with the following connector brands:
CONNECTOR
TYPE
Dual-rated
Aluminum
Splices
Dual-rated
Aluminum
Lugs
ANDERSON
VACS
VACL
BLACKBURN
ASP
ATL
®
BURNDY
YS-A
YA-A
YA-ATN
ILSCO
AS
ASN
ACL/ACN
2ACL/2ACN
ALNS/ALNN/ALND
PANDUIT
SA
LAA
LAB
T&B
60501 to
60578
60101 to
60176;
60230 to
60278
BCU
BBCU
BLU
BBLU
PENNUNION
PIK
BLUA
NUMBER
OF CRIMPS*
8 AWG to
250 kcmil:
1 crimp
300 to
750 kcmil:
2 crimps
NUMBER
OF CRIMPS*
8 to
1/0 AWG:
1 crimp
2/0 AWG to
350 kcmil:
2 crimps
400 to
750 kcmil:
3 crimps
* Use the number of
95R7
crimps listed in this
column instead of the
number provided with
the connector.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
16
Page 17
E12CCXL 12-ton Battery-powered Tool
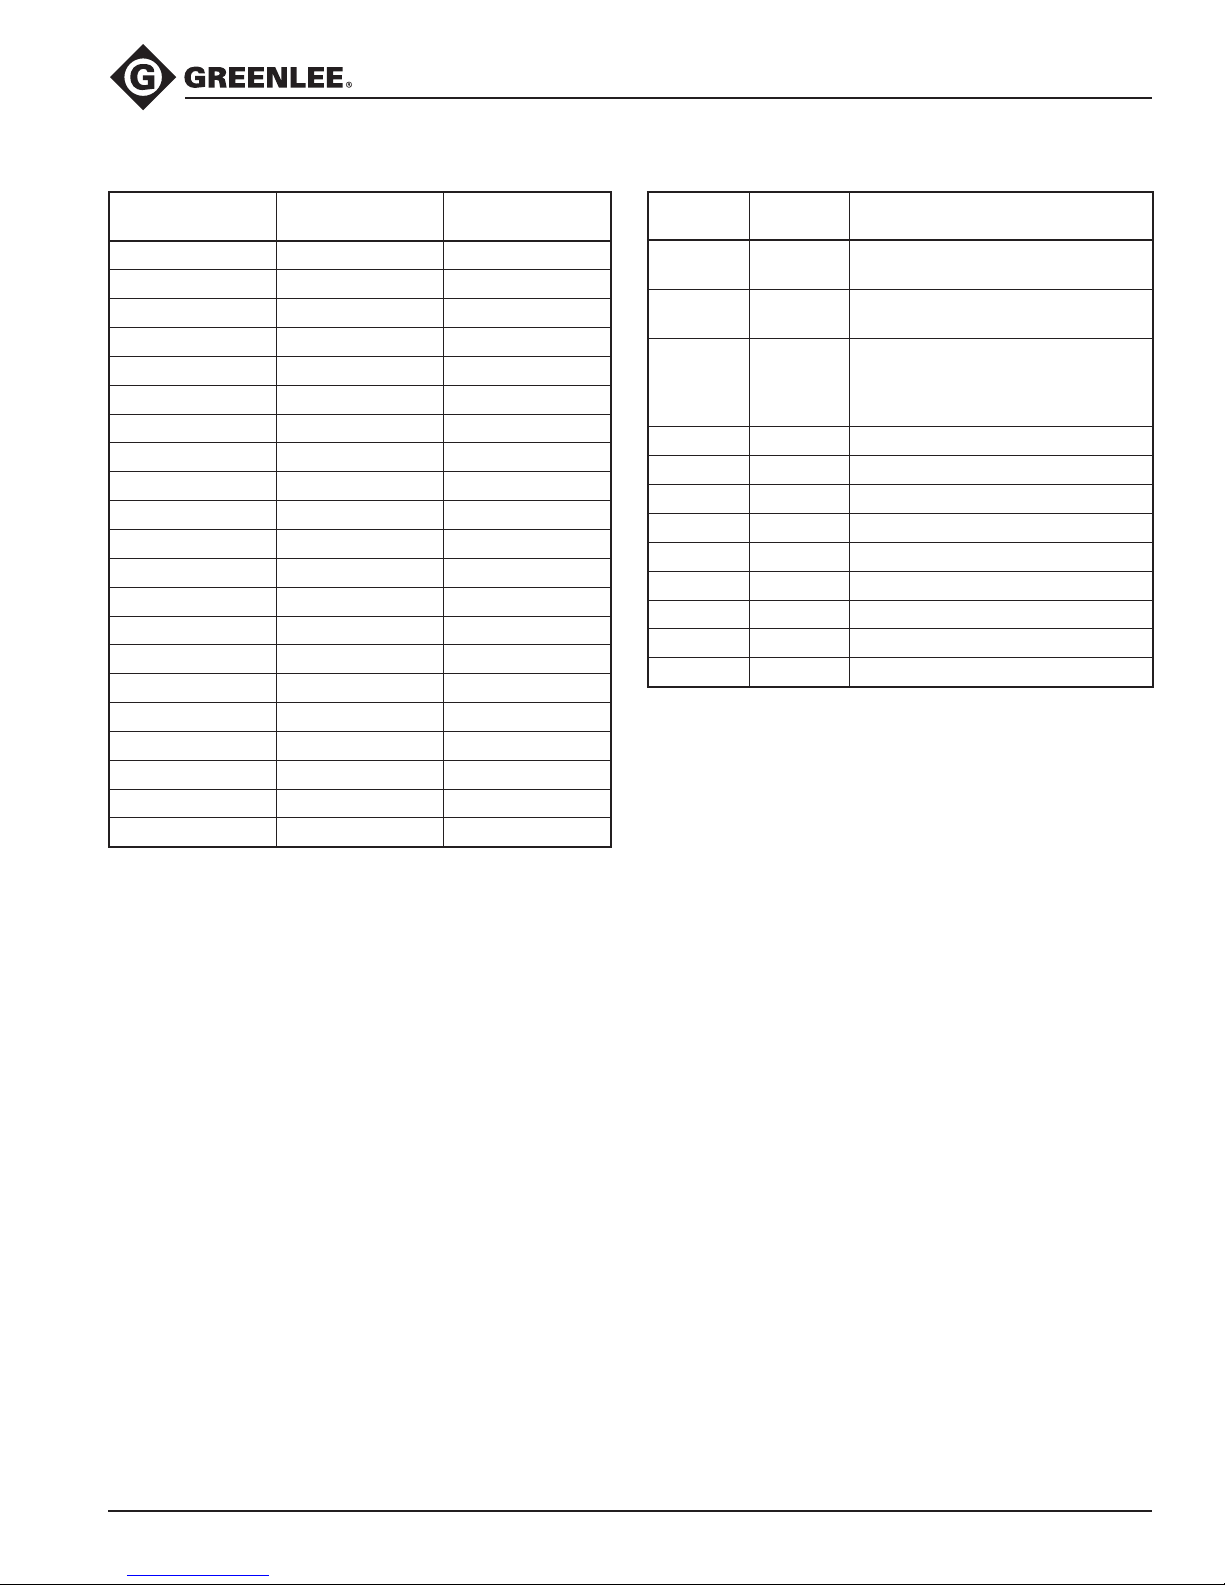
Additional U-type Dies
Greenlee
Catalog No.
KD12-10 10188 U-BG
KD12-11 10189 U-0
KD12-12 10190 U-C
KD12-14 10192 U-161
KD12-15 10193 U-162
KD12-16 10194 U-163
KD12-17 10195 U-165
KD12-18 10196 U-166
KD12-19 10197 U-243
KD12-20 10198 U-247
KD12-21 10199 U-249
KD12-30 10200 U-D3
KD12-31 10201 U-E
KD12-32 10202 U-F
KD12-33 10203 U-997
KD12-35 10205 U-238
KD12-36 10206 U-654
KD12-37 10207 U-655
KD12-38 10208 U-658
KD12-39 10209 U-659
KD12-40 10210 U-998
Greenlee
UPC No.
FCI Burndy
No.
Available Accessories
Adapter
UC26 50067141
UC40 50070363
UCACSR 50070371
UCUNC14 50070380 Cutter blades for 1/4" threaded rod
UCUNC38 50070398 Cutter blades for 3/8" threaded rod
UCUNC12 50072749 Cutter blades for 1/2" threaded rod
UA12P 50118900 Punch driver adapter
04686 50046861 Die bushing*
12185 50121855 Spacer*
03170 50031708 Punch sleeve, 1-1/8"*
UA12T 52020102 Adapter for U-type dies
UA12ID 52061814 Dieless die set
*
Required for knockout punches larger than 4" actual diameter.
Greenlee
Part No.
Description
Cutter blades for copper and
aluminum 26 mm (1") max.
Cutter blades for copper and
aluminum 40 mm (1-1/2") max.
Cutter blades for ACSR, ACAR,
standard guy wire, EHS guy wire,
copperweld, ground rod, anchor
rod, soft bolts, rebar
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
17
Page 18
E12CCXL 12-ton Battery-powered Tool
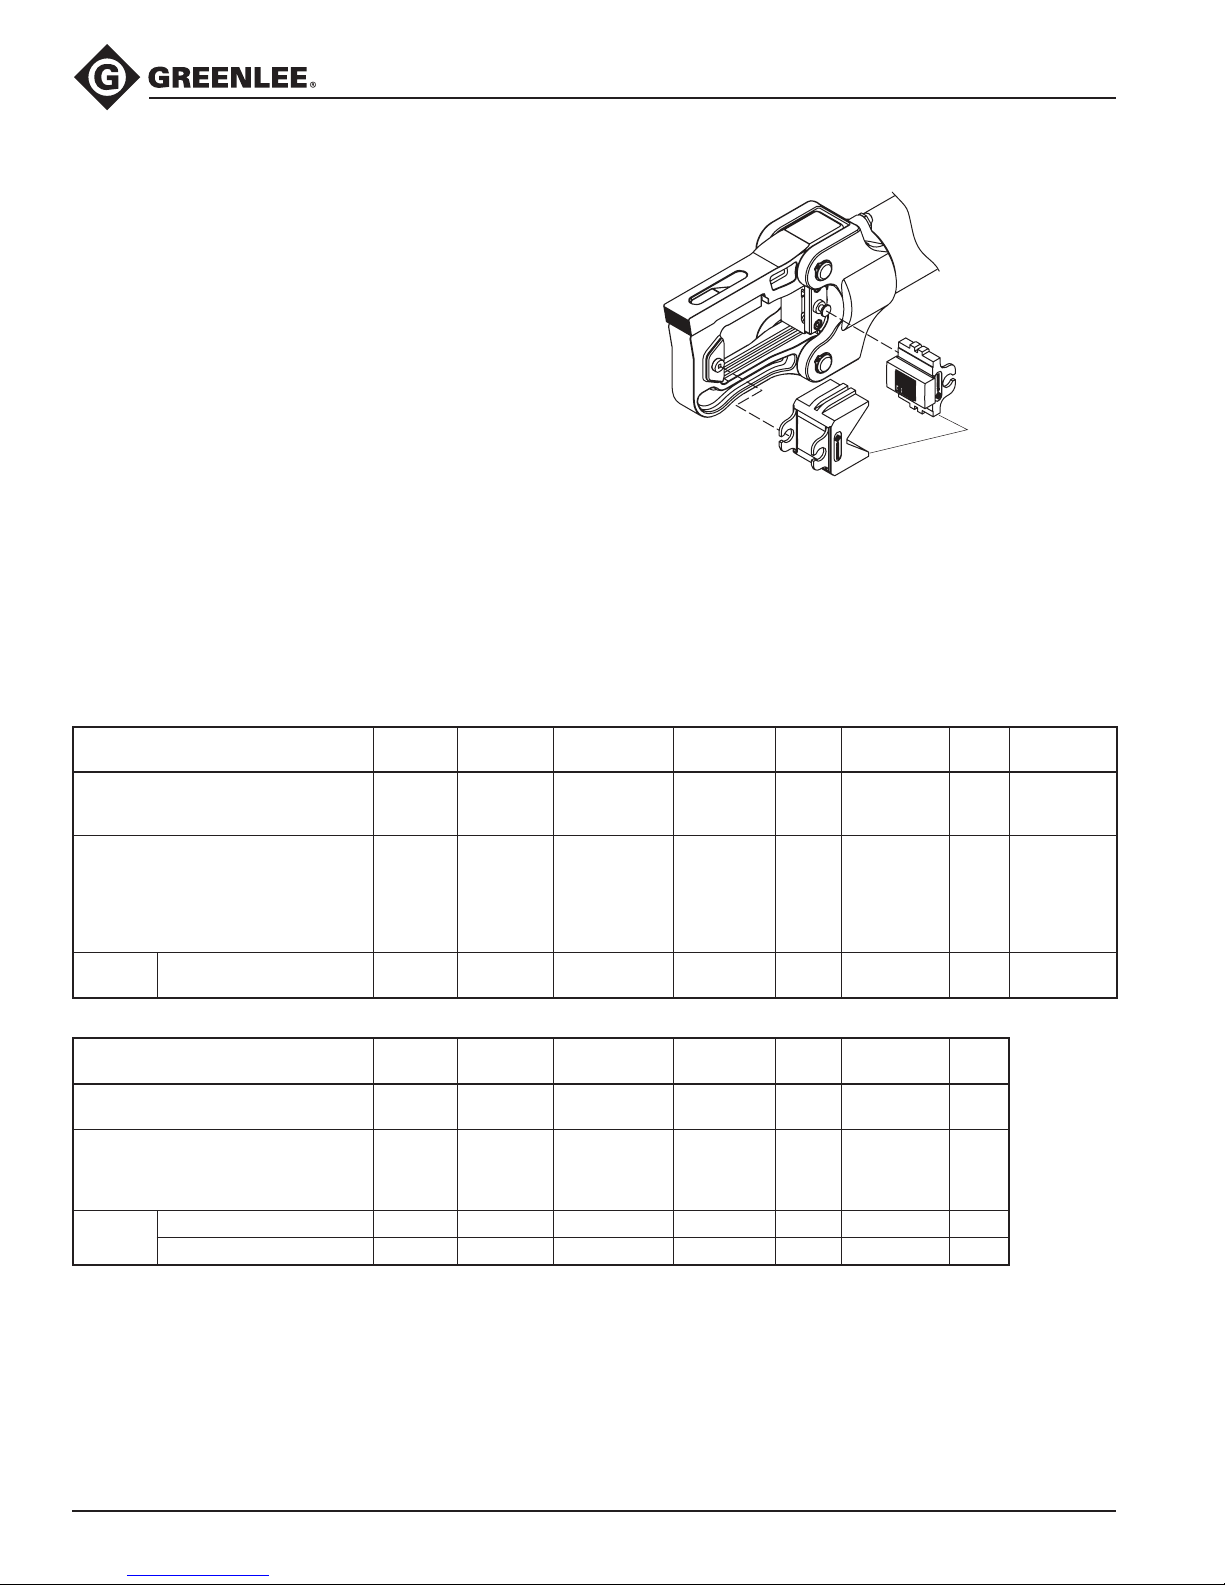
cUL and UL Classified Crimps
Crimps made with the Greenlee UA12ID dieless die and
E12CCXL crimping tool are cUL and UL classied on
standard concentric, compressed, or compact stranded
copper and aluminum cable with the connectors listed
here.
Refer to the
and model numbers of appropriate connectors and the
number of crimps required.
Connector Table (NOT for use with flex, navy or welding wire)
“Connector Table”
for the brand names
UA12ID
Dieless Die Set
Range: Copper Connectors—4 AWG to 750 kcmil
Aluminum Connectors—6 AWG to 600 kcmil
COPPER CONNECTOR TYPE ANDERSON BLACKBURN
Copper Splices
Copper Lugs
*Number of
Crimps
ALUMINUM CONNECTOR TYPE ANDERSON BLACKBURN
Dual-Rated Aluminum Splices VACS ASP YS-A
Dual-Rated Aluminum Lugs VACL ATL
*Number of
Crimps
Copper Cable Size:
4 AWG–750 kcmil
Cable Size: 6 AWG–500 kcmil 1 1 1 1 1 1 1
Cable Size: 600 kcmil 2 1 1 1 2 1 1
VHSS
VHS
VHCS
VHCL
1 1 1 1 1 1 1 1
®
CSP
CU
CTL
CTL-L
LCN
®
BURNDY ILSCO PANDUIT T & B
YS-L
YS
YA, YA-L, YA-2L
YA-2LN, YA-2N
YA-L-TC, YA-L-2TC
YA-2TC, YAZ
YAZ-2N, YAZ-2TC
BURNDY ILSCO PANDUIT T & B
YA-A
YA-A-TN
CT
CTL
CLN, CLW, CSW
CRA, CRB, CRC
CRA-L, CRB-L
CRA-2L
CRB-2L
CRC-2L
AS
ASN
ACL, ACN
2ACL, 2ACN
ALNS, ALNN
ALND
SCSS
SCS
SCL, SCH
LCAS
LCA
LCB
LCD, LCC
LCAN
SA 60507 to 60584
LAA
LAB
54506 to 54528
54806 to 54828
54106 to 54128
54206 to 54228
54906BE to
54928BE
54854BE to
54882BE
60106 to 60184
60230 to 60284
PENN-
UNION
BCU
BBCU
BLU
BBLU
PENN-
UNION
PIK
BCUA
BLUA
TYCO (AMP)
—
1099898-2 to
1-1099898-5
1099899-2 to
1-1099899-9
1099939-1 to
1-1099939-5
* When crimping with the UA12ID dieless die set, use the number of crimps listed in this table
instead of the number provided with the connector.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
18
Page 19
Maintenance
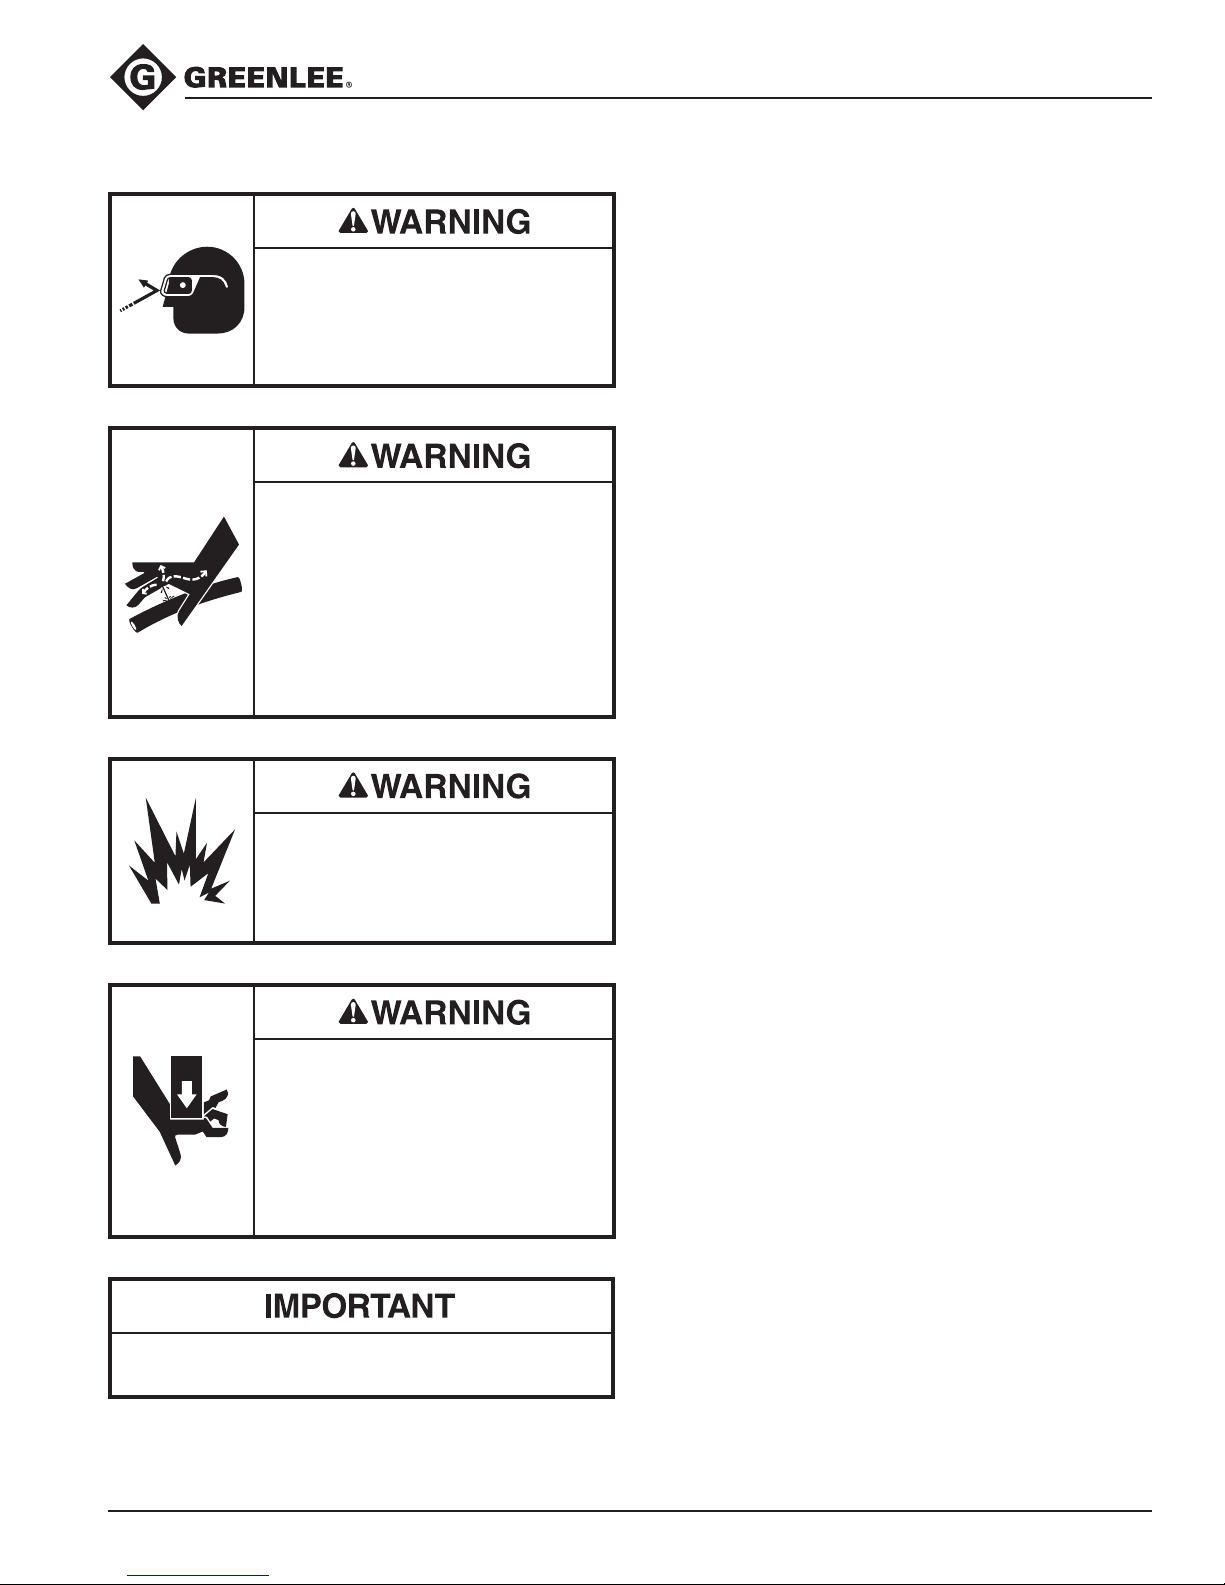
Wear eye protection when operating
or servicing this tool.
Failure to wear eye protection could
result in serious eye injury from
ying debris or hydraulic oil.
Skin injection hazard:
Do not use hands to check for oil
leaks. Oil under pressure easily
punctures skin. If injured, seek
medical attention immediately to
remove oil.
Failure to observe this warning
could result in serious injury, gangrene, or death.
E12CCXL 12-ton Battery-powered Tool
Daily
Before use:
1. Inspect the tool for wear or damage, such as cracks,
gouges, or chips.
2. Inspect the tool for damage or leaks.
3. Inspect the rotation of the head assembly. Fully
retract the ram. The head should rotate no more
than 360°. If damage is detected, send the tool to a
Greenlee Authorized Service Center for inspection.
After use:
1. Use a damp cloth and mild detergent to clean the
housing. Allow the housing to dry.
2. Fully retract the ram. Place the tool in the carrying
case and store in a cool, dry place.
3. If necessary, recharge the batteries. Refer to the
instructions supplied with the battery charger.
Monthly
1. Thoroughly clean all surfaces.
2. Check the oil level.
Do not use solvents or ammable
liquids to clean the tool body.
Solvents or ammable liquids could
ignite and cause serious injury or
property damage.
Pinch points:
• Remove battery before changing
dies, adapters, or jaws.
• Keep hands away from the crimping tool head when crimping.
Failure to observe these warnings
could result in severe injury or death.
Annually or After 10,000 Crimps
1. Replace the hydraulic oil.
2. Send the tool to a Greenlee Authorized Service
Center for inspection.
Checking the Oil Level
1. Remove the screws holding the housing cover
together.
2. Point the crimping head downward and remove the
oil reservoir plug. Fill reservoir if necessary.
3. Replace the oil plug and housing cover.
Periodic Pressure Relief Valve Check
The crimping tool’s relief valve may require occasional
adjustment. To determine whether this adjustment is
necessary, periodically send the tool to an authorized
service center.
Note: For Warranty Service or Repair, contact Greenlee
customer service at 800-435-0786.
Relief valve adjustments must be done by an
authorized service center.
Greenlee / A Textron Company 4455 Boeing Dr. • Rockford, IL 61109-2988 USA • 815-397-7070
19
Page 20
Troubleshooting
E12CCXL 12-ton Battery-powered Tool
Before You Begin
1. Make sure that the battery is charged. Recheck
the battery after several minutes to make sure the
battery is holding its charge.
2. Use a nonflammable contact cleaner or pencil
eraser to clean the electrical contacts on the battery
and tool.
3. Reinstall the battery and check the tool again.
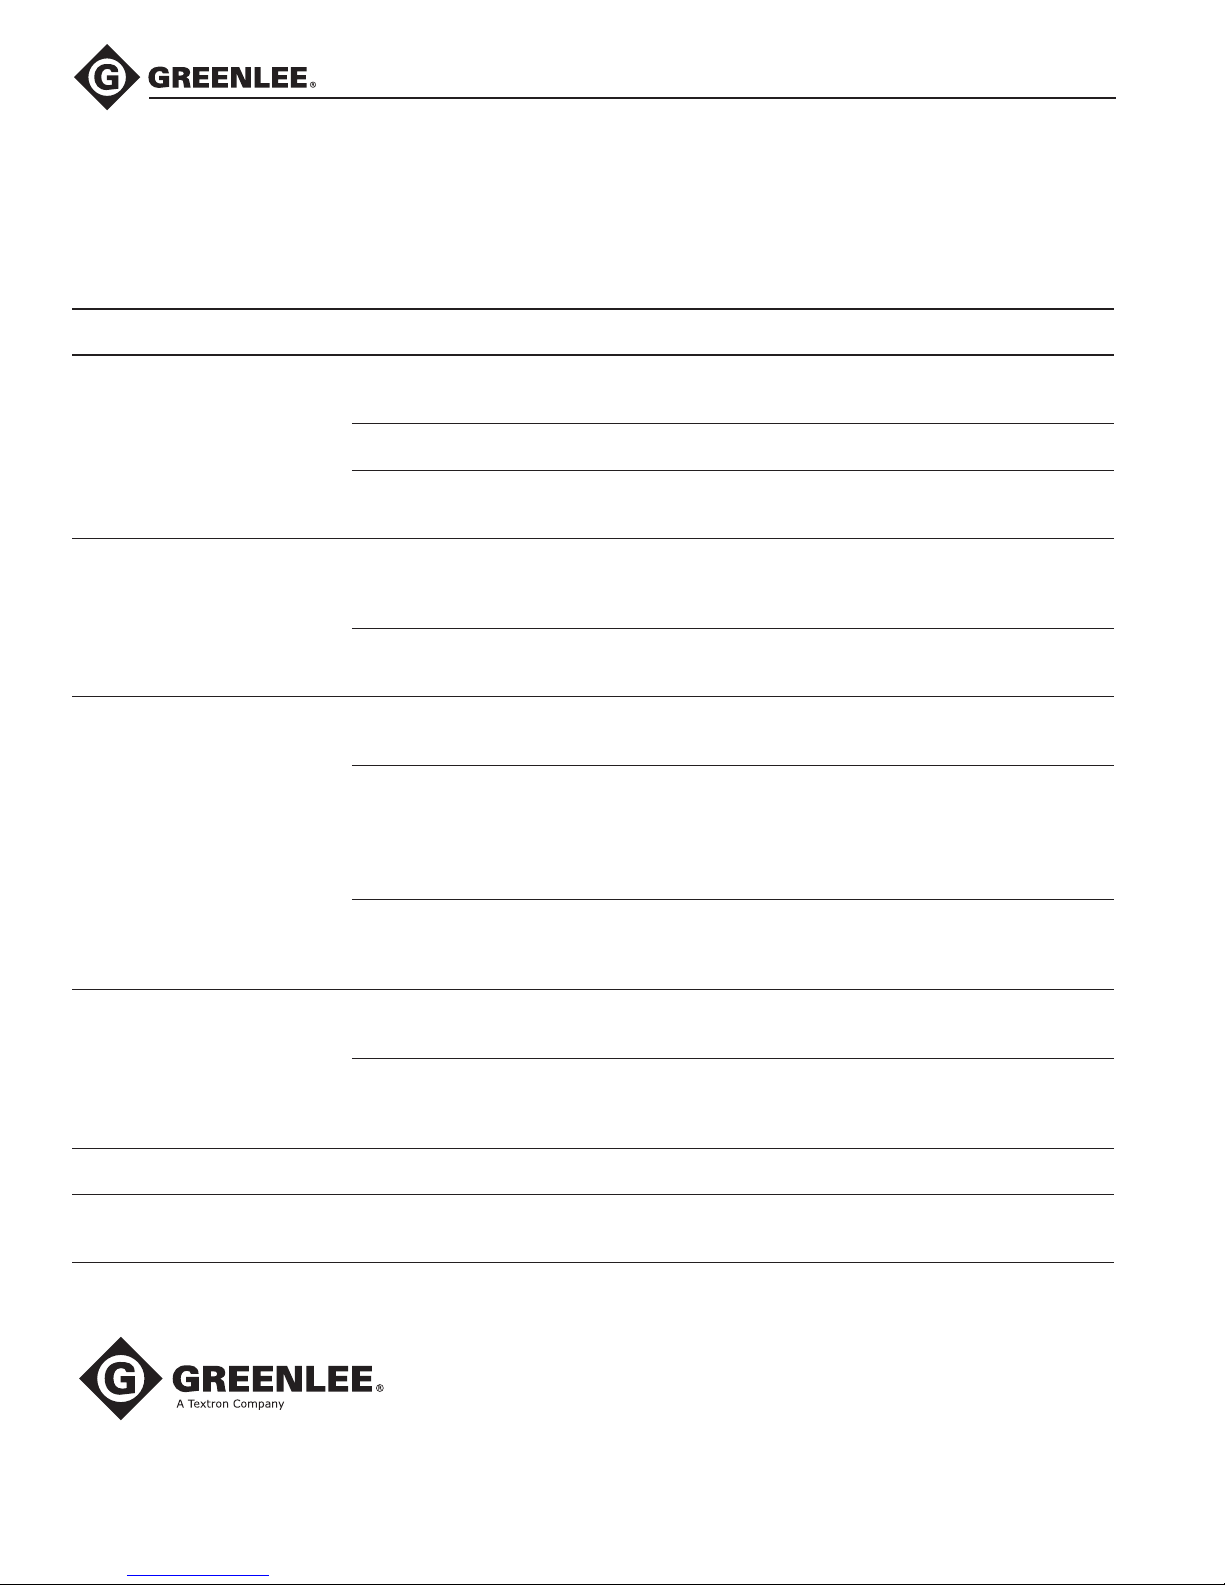
Problem Possible Cause Probable Remedy
Tool is inoperative. Dirt, contaminants, etc., in ram area
Clean tool.
oftool.
Tool battery contacts damaged. Reform contacts.
Tool components worn or damaged. Return tool to a Greenlee Authorized
Service Center.
Motor is inoperative. Low or uncharged battery. Try known charged battery. Inoperative
battery may be discharged or may have
reached life expectancy.
Broken switch components. Return tool to a Greenlee Authorized
Service Center.
Motor runs but tool will not
complete a cycle.
Oil level low. Return tool to a Greenlee Authorized
Service Center.
Air in hydraulic system. Pull trigger and hold retract button
simultaneously. Run for approximately
10 seconds, and then attempt to
crimp. If unsuccessful, return tool to a
Greenlee Authorized Service Center.
Cold oil. Pull trigger and hold retract button
simultaneously to warm oil. Store tool
in warm area.
Dies stop during operation. Oil level low. Return tool to a Greenlee Authorized
Service Center.
Air in hydraulic system. Pull trigger and hold retract button
simultaneously. Hold for approximately
10 seconds.
LED glows for 20 seconds. Battery charge low. Charge or replace battery.
Tool loses oil. Damaged internal seal. Return tool to a Greenlee Authorized
Service Center.
Note: For Warranty Service or Repair, contact Greenlee customer service at 800-435-0786.
4455 Boeing Drive • Rockford, IL 61109-2988 • USA • 815-397-7070
An ISO 9001 Company • Greenlee Textron Inc. is a subsidiary of Textron Inc.
www.greenlee.com
USA Tel: 800-435-0786
Fax: 800-451-2632
Canada Tel: 800-435-0786
Fax: 800-524-2853
International Tel: +1-815-397-7070
Fax: +1-815-397-9247
 Loading...