

Page 1
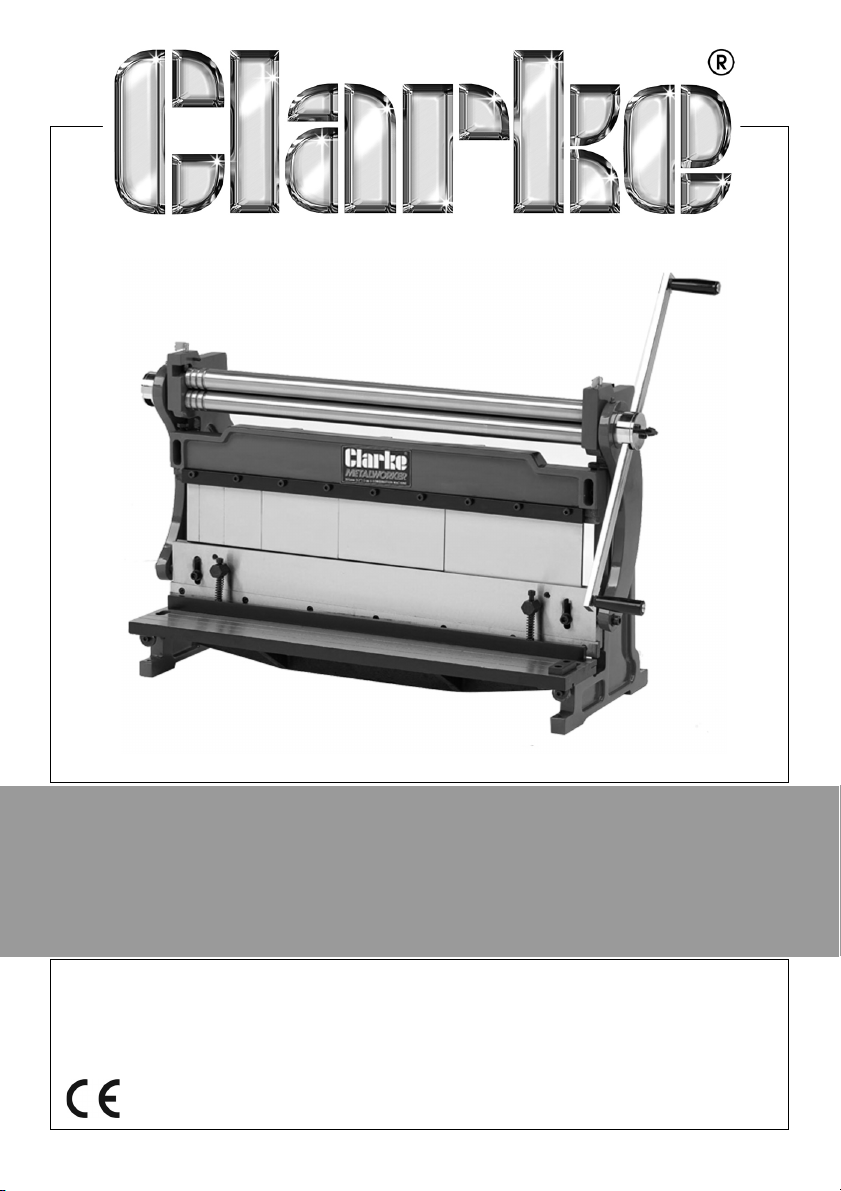
3 IN1 SHEET METAL MACHINE
MODEL NO: SBR760
PART NO: 6560030
OPERATION & MAINTENANCE
INSTRUCTIONS
LS0620 ISS 3
Page 2
INTRODUCTION
Thank you for purchasing this CLARKE 3 in1 Sheet Metal Machine.
Before attempting to use this product, please read this manual thoroughly and
follow the instructions carefully. In doing so you will ensure the safety of yourself
and that of others around you, and you can look forward to your purchase
giving you long and satisfactory service.
GUARANTEE
This product is guaranteed against faulty manufacture for a period of 12
months from the date of purchase. Please keep your receipt which will be
required as proof of purchase.
This guarantee is invalid if the product is found to have been abused or
tampered with in any way, or not used for the purpose for which it was
intended.
Faulty goods should be returned to their place of purchase, no product can
be returned to us without prior permission.
This guarantee does not effect your statutory rights.
FEATURES
• Shear Table Front Guide
• Shear & Brake Adjustable Rear Stop
• Hardened Steel Brake Fingers
• Precision Ground Hardened Steel Shear Blade
2
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 3
SAFETY INSTRUCTIONS FOR MACHINERY
1. READ THE ENTIRE MANUAL BEFORE USE. Machinery presents serious injury
hazards to untrained users.
2. ALWAYS USE APPROVED SAFETY GLASSES WHEN OPERATING MACHINERY.
Everyday eyeglasses are NOT safety glasses.
3. ALWAYS USE HEARING PROTECTION WHEN OPERATING MACHINERY.
Machinery noise can cause permanent hearing loss.
4. WEAR PROPER APPAREL. DO NOT wear loose clothing, gloves, neckties,
rings, or jewellery that can catch in moving parts. Wear protective hair
covering to contain long hair and wear non-slip footwear.
5. NEVER OPERATE MACHINERY WHEN TIRED OR UNDER THE INFLUENCE OF
DRUGS OR ALCOHOL. Be mentally alert at all times when in use.
6. ONLY ALLOW TRAINED AND PROPERLY SUPERVISED PERSONNEL TO OPERATE
MACHINERY. Make sure operation instructions are safe and understood.
7. KEEP CHILDREN AND VISITORS AWAY from the work area.
8. MAKE WORKSHOP CHILDPROOF. Use padlocks, master switches, and
remove start switch keys.
9. DO NOT USE IN DANGEROUS ENVIRONMENTS. DO NOT use machinery in
damp, wet locations, or where any flammable or noxious fumes may exist.
10. KEEP WORK AREA CLEAN AND WELL LIGHTED. Clutter and dark shadows
may cause accidents.
11. MAINTAIN MACHINERY WITH CARE. Keep blades sharp and clean for best
and safest performance.
12. MAKE SURE GUARDS ARE IN PLACE AND WORK BEFORE USING MACHINERY.
13. REMOVE ADJUSTING KEYS AND WRENCHES. Make a habit of checking for
keys and adjusting wrenches before turning machinery ON.
14. CHECK FOR DAMAGED PARTS BEFORE USING MACHINERY. Check for
binding or misaligned parts, broken parts, loose bolts, and any other
conditions that may impair machine operation. Repair or replace
damaged parts before operation
15. USE RECOMMENDED ACCESSORIES. Refer to the instruction manual for
recommended accessories. Improper accessories increase risk of injury.
16. DO NOT FORCE MACHINERY. Work at the speed for which the machine or
accessory was designed.
17. DO NOT OVER REACH. Maintain stability and balance at all times.
3
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 4
ADDITIONAL SAFETY INSTRUCTIONS FOR 3-IN-1 SHEET METAL MACHINES
1. OVERLOADING. Attempting to overload this machine beyond the
capacities specified in the “Specifications” on page 35 could cause
personal injury or property damage. DO NOT extend the hand crank to
apply additional force.
2. USAGE. To avoid injury or property damage, always use the machine for its
intended purposes, DO NOT modify the machine in any way.
3. METAL EDGES. Sharp metal edges can cut your fingers. ALWAYS chamfer
and de-burr sharp sheet metal edges before bending and after cutting the
workpiece.
4. PINCHING. This machine represents severe pinching and amputation
hazards. ALWAYS keep hands away from the rollers, brake fingers, clamping
bar, and shearing blades when operating.
5. PERSONAL PROTECTION. To avoid personal injury, ALWAYS wear heavy
leather gloves, eye protection, and leather boots with extra toe protection
when using this machine.
6. BODY POSITION. To avoid injury due to slipping or falling, ALWAYS maintain
secure footing and a comfortable body position when using this machine.
7. GOOD WORKING CONDITION. To reduce the risk of personal injury, ALWAYS
inspect the working parts of this machine for cracks, burrs, loose fasteners,
or any other damage and resolve any issue before beginning operation.
8. WORKBENCH MOUNTING. Personal injury could occur if this machine should
unexpectedly move during operation. ALWAYS make sure the machine is
securely mounted to a stable workbench or stand that can support the
weight and pressures of the operation.
9. ENTANGLEMENT HAZARDS. The moving parts of this machine represent
entanglement hazards. DO NOT wear jewelry, or loose clothing, and tie
back long hair when using this machine.
10. SHEARING BLADES/BRAKE FINGERS. If not properly aligned, the shearing
blades or brake fingers can cause machine parts or the workpiece to
break up and fly towards the operator. ALWAYS keep these parts properly
adjusted and in good working condition..
4
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 5
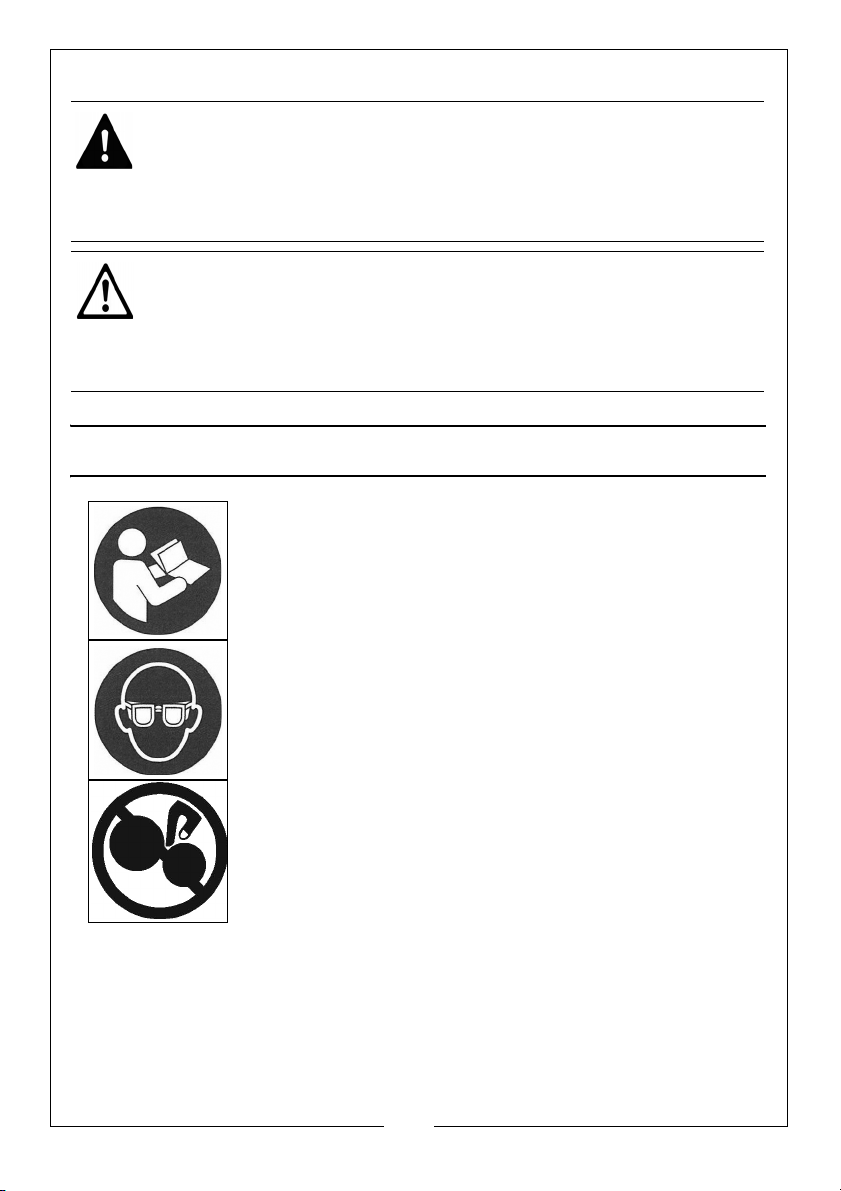
WARNING: LIKE ALL MACHINERY THERE IS POTENTIAL DANGER WHEN
OPERATING THIS MACHINE. ACCIDENTS ARE FREQUENTLY CAUSED BY
LACK OF FAMILIARITY OR FAILURE TO PAY ATTENTION. USE THIS MACHINE
WITH RESPECT AND CAUTION TO DECREASE THE RISK OF OPERATOR
INJURY. IF NORMAL SAFETY PRECAUTIONS ARE OVERLOOKED OR
IGNORED, SERIOUS PERSONAL INJURY MAY OCCUR.-
CAUTION: NO LIST OF SAFETY GUIDELINES CAN BE COMPLETE. EVERY
WORKSHOP ENVIRONMENT IS DIFFERENT. ALWAYS CONSIDER SAFETY
FIRST, AS IT APPLIES TO YOUR INDIVIDUAL WORKING CONDITIONS. USE
THIS AND OTHER MACHINERY WITH CAUTION AND RESPECT. FAILURE TO
DO SO COULD RESULT IN SERIOUS PERSONAL INJURY, DAMAGE TO
EQUIPMENT, OR POOR WORK RESULTS.
WARNING LABELS
Read this manual before use.
Wear eye protection when using the machine.
Keep fingers clear of break, dies, rollers and blade.
5
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 6
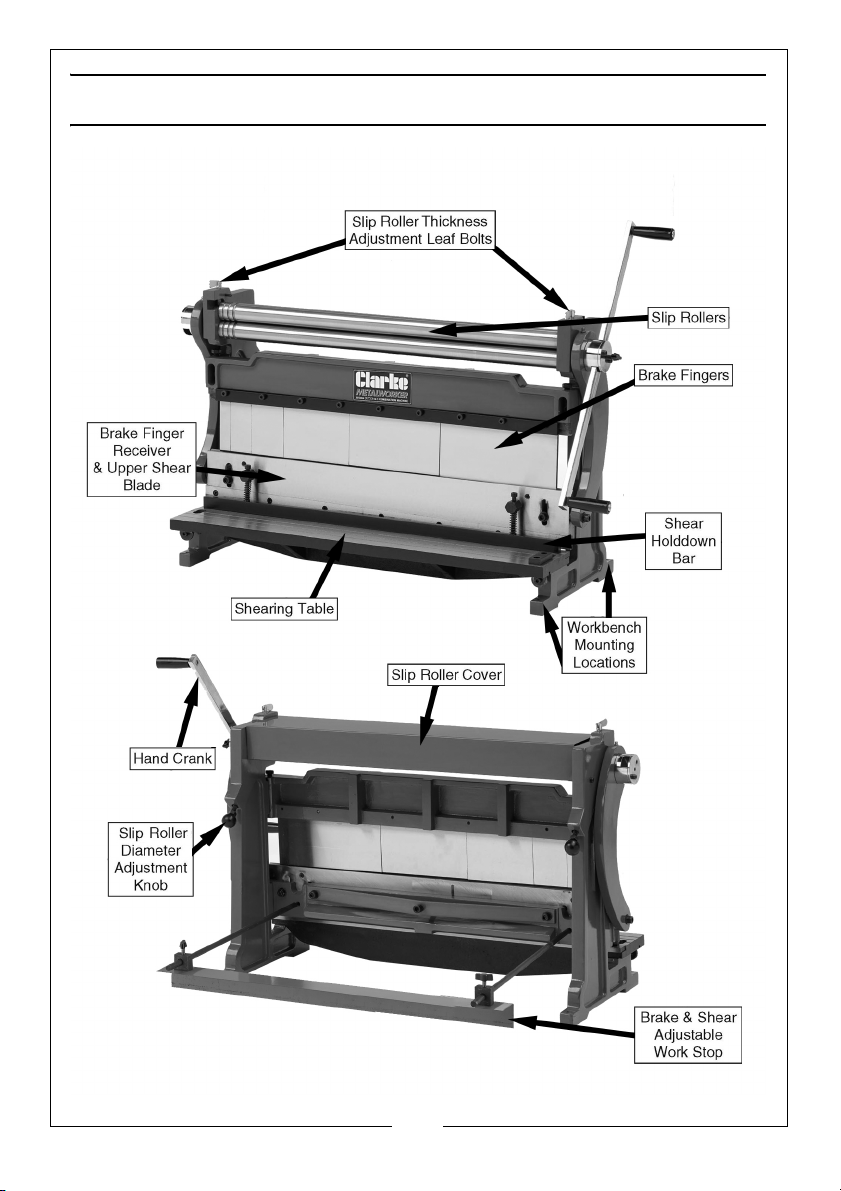
PARTS IDENTIFICATION
Fig. 1
6
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 7
SETUP
Fig. 2
Fig. 3
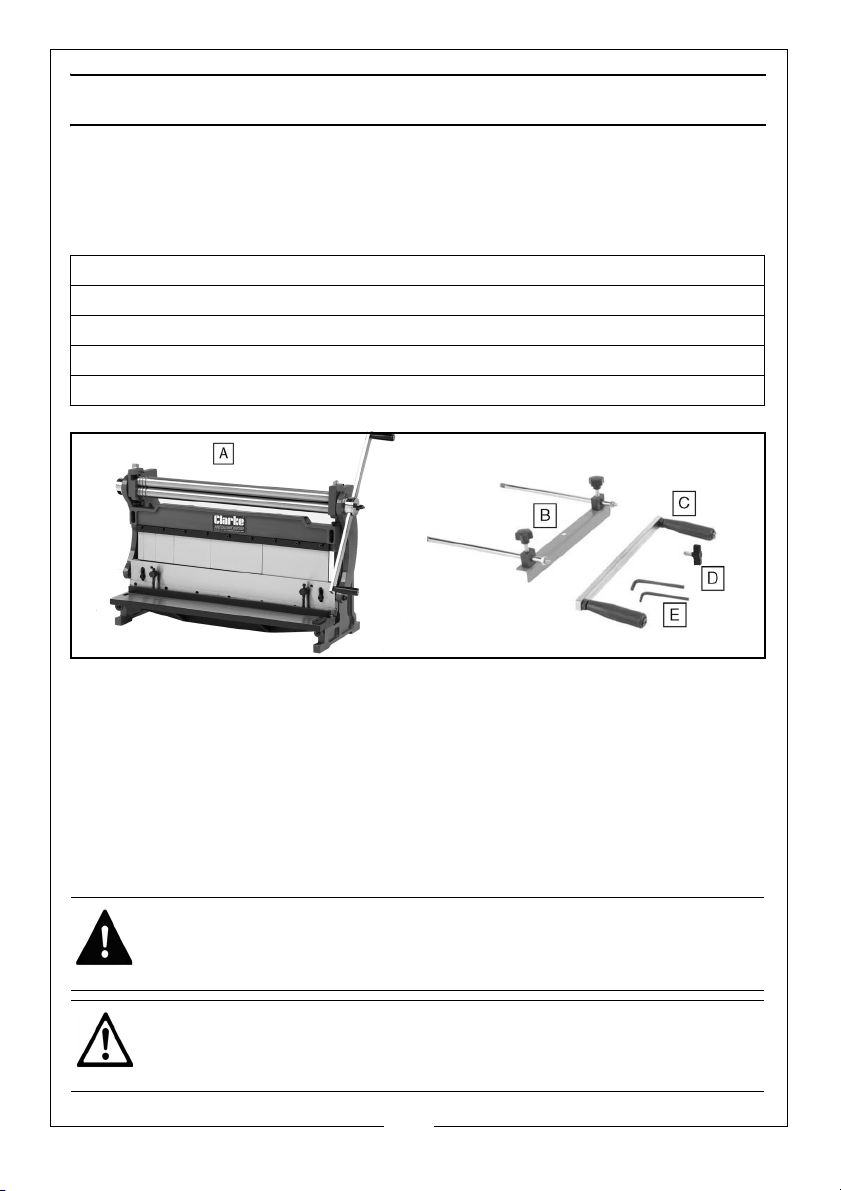
UNPACKING
Remove the packaging materials from around your machine and make sure
that you have the following items. If you discover the machine is damaged in
any way, please contact your Clarke dealer.
A. Sheet Metal Machine
B. Shear & Brake Rear Work Stop
C. Hand Crank Handle
D. Hand Crank Lock Knobs
E. Hex Wrenches
CLEAN UP
The unpainted surfaces are coated with a waxy oil to prevent corrosion during
shipment. Remove this protective coating with a solvent cleaner or degreaser.
For thorough cleaning, some parts must be removed.
For optimum performance, clean all moving parts or sliding contact surfaces.
Avoid chlorine-based solvents, such as acetone or brake parts cleaner that
may damage painted surfaces.
Always follow the manufacturer's instructions when using cleaning products.
WARNING: PETROL AND PETROLEUM BASED PRODUCTS HAVE LOW
FLASHPOINTS AND CAN EXPLODE OR CAUSE FIRE IF USED TO CLEAN
MACHINERY. DO NOT USE THESE PRODUCTS TO CLEAN THE MACHINERY.
CAUTION: MANY CLEANING SOLVENTS ARE TOXIC IF INHALED. MINIMIZE
YOUR RISK BY ONLY USING THESE PRODUCTS IN A WELL VENTILATED
AREA.
7
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 8
SITE CONSIDERATIONS
Fig. 4
Fig. 5
Fig. 6
FLOOR LOAD
Refer to the Specifications for the weight and footprint specifications of your
machine. Some workbenches or stands may require additional reinforcement
to support the machine, workpiece, and the forces applied during operation.
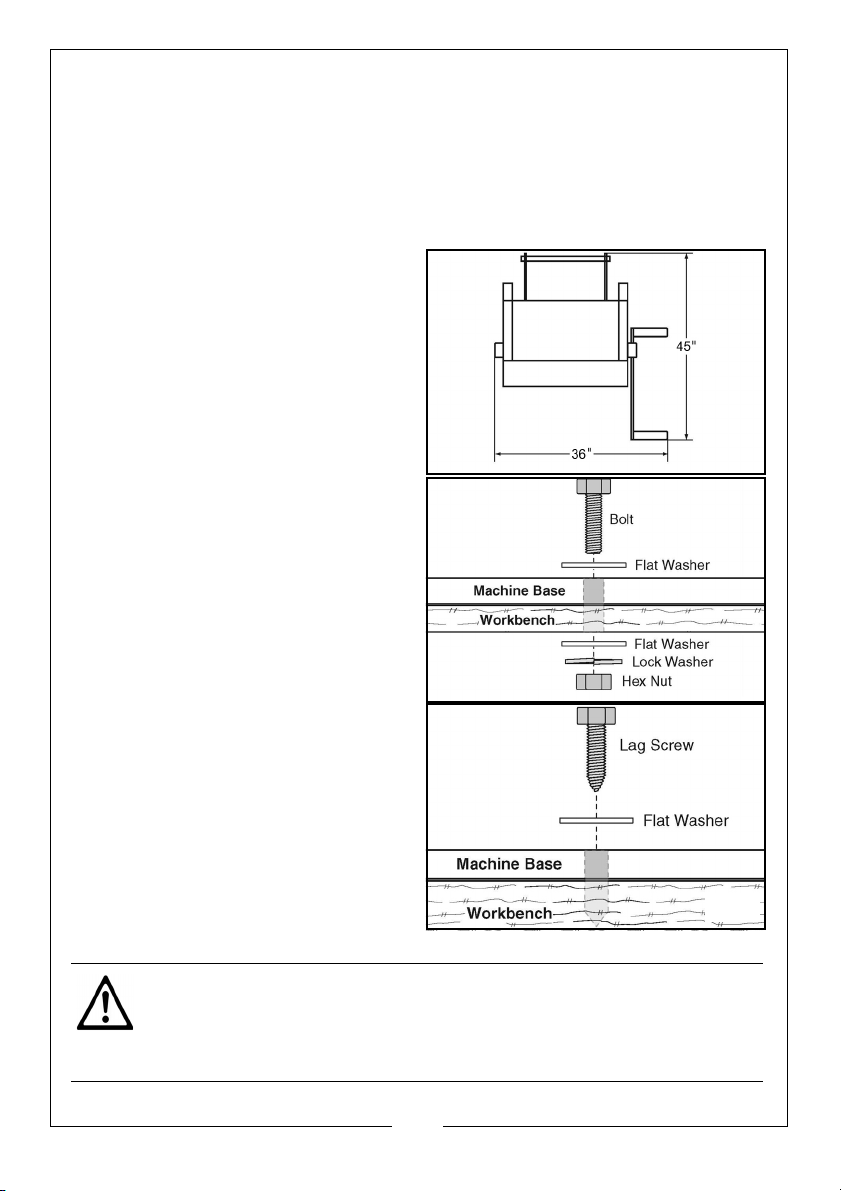
PLACEMENT LOCATION
Consider existing and anticipated
needs, size of material to be
processed through each machine,
and space for auxiliary stands, work
tables or other machinery when
establishing a location for your new
machine. See Figure 4 for the
minimum working clearances.
MOUNTING
The base of this machine has holes
that allow it to be mounted to a
workbench. For a safe and smooth
operation of this machine, it MUST be
securely mounted to an appropriate
workbench or stand.
The strongest mounting option is a
“Through Mount” (Figure 5) where
holes are drilled all the way through
the workbench, and hex bolts,
washers, and hex nuts are used to
secure the machine to the
workbench.
Another option for mounting is a
“Direct Mount” (Figure 6) where the
machine is simply secured to the
workbench with a lag screw.
CAUTION: DUE TO THE CONSIDERABLE FORCES EXERTED ON THIS
MACHINE WHEN IN OPERATION, YOU MUST SECURELY MOUNT IT TO A
STABLE AND STURDY WORKBENCH OR STAND. OTHERWISE, THE MACHINE
COULD TIP OR FALL AND RESULT IN PERSONAL INJURY OR PROPERTY
DAMAGE.
8
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 9
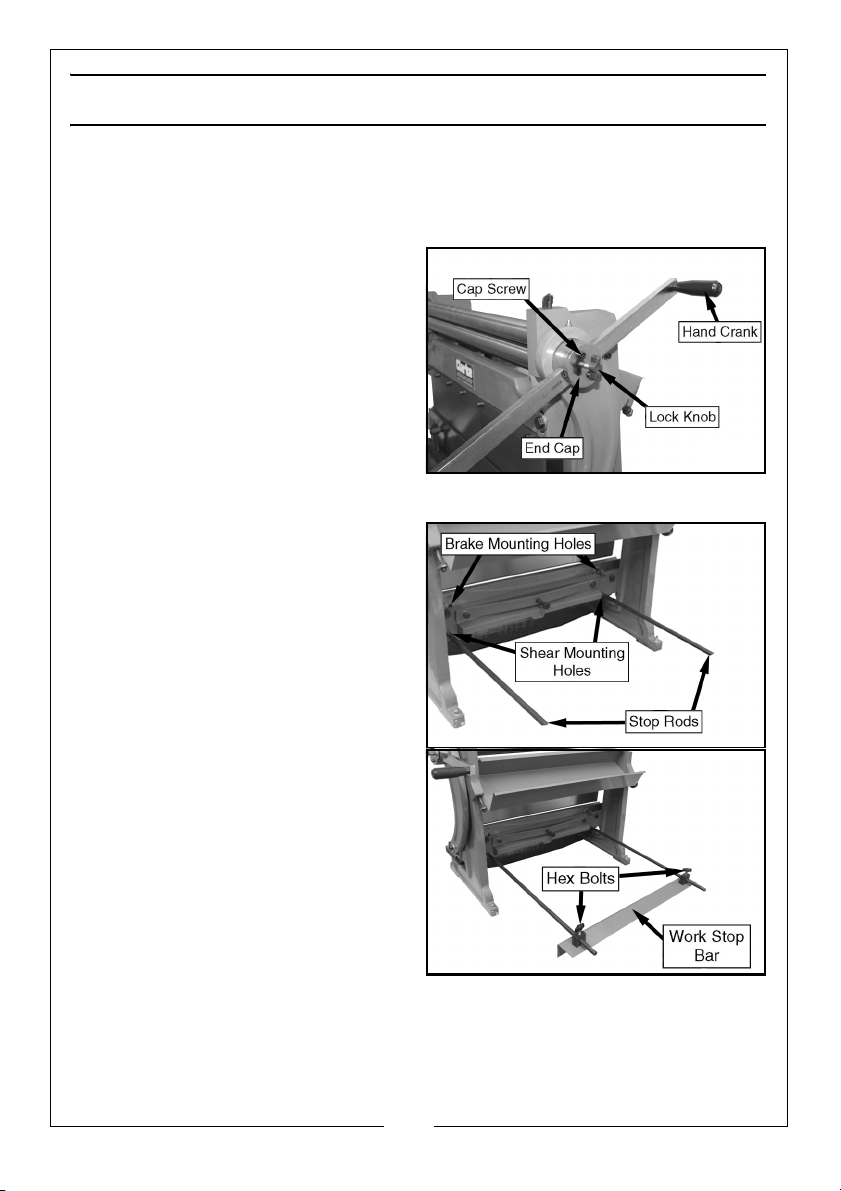
ASSEMBLY
Fig. 7
Fig. 8
Fig. 9
In addition to the assembly procedures below, some disassembly is required to
remove storage grease and re-lubricate the cleaned parts.
TO ASSEMBLE YOUR MACHINE:
1. Remove the end cap screws from
the end cap.
2. Rotate the lock knob out until it is
flush with the rear of the end cap.
3. Insert the hand crank into the slot
(see Figure 7).
4. Replace the end cap and cap
screws and tighten the lock knob.
NOTE: It is your preference which
side of the machine you install the hand crank.
5. Thread the rods into either the
brake or sheer mounting holes, as
shown in Figure 8. Only handtighten the rods.
6. Loosen the hex bolts on the stop
bar and slide it onto the rods.
7. Position the stop bar as required
and secure using the hex bolts as
shown in Figure 9.
9
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 10
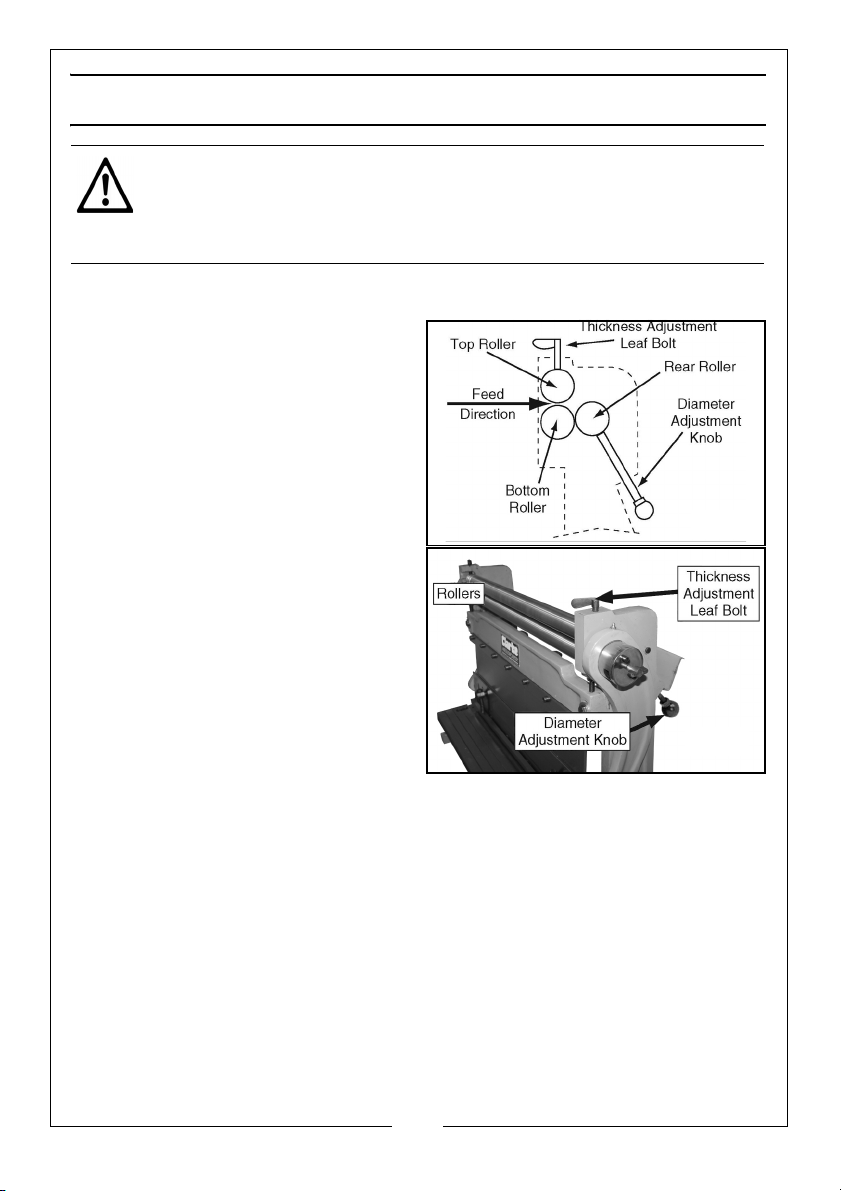
OPERATING - SLIP ROLLERS
Fig. 10
Fig. 11
CAUTION: THE ROLLERS OF THIS MACHINE PRESENT A PINCHING
HAZARD. MAKE SURE NO BODY PART OR CLOTHING IS NEAR THE
ROLLERS DURING OPERATION. FAILURE TO FOLLOW THIS WARNING MAY
RESULT IN FINGERS, HAIR, OR CLOTHING BEING PULLED INTO THE
MACHINE, CAUSING PERSONAL INJURY.
SLIP ROLLER OVERVIEW
The slip roller is used to form cylinders,
cones, and arcs in sheet metal up to
1 mm in thickness and 760 mm wide,
as well as wires and rods. Three steel
rollers are configured to draw the
workpiece through a path that will
produce the desired results (see
Figures 10-11).
SLIP ROLLING TIPS
• Due to the many variables of different sheet metal types, no single
configuration of the rollers will create the same curve on all materials.
Rolling sheet metal to achieve an exact radius is a trial-and-error
process.
• Performing multiple passes through the machine with gradual
reductions in the curve radius produces better results than trying to
make the curve in one pass.
• To avoid pitted workpieces and damage to the roller surfaces, always
make sure the workpiece and the rollers are free of grit and any foreign
material before every use.
• Unless the operation requires a cone-type curve, always keep the rear
roller parallel to the front rollers by rotating the diameter adjustment
knobs the same amount.
10
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 11
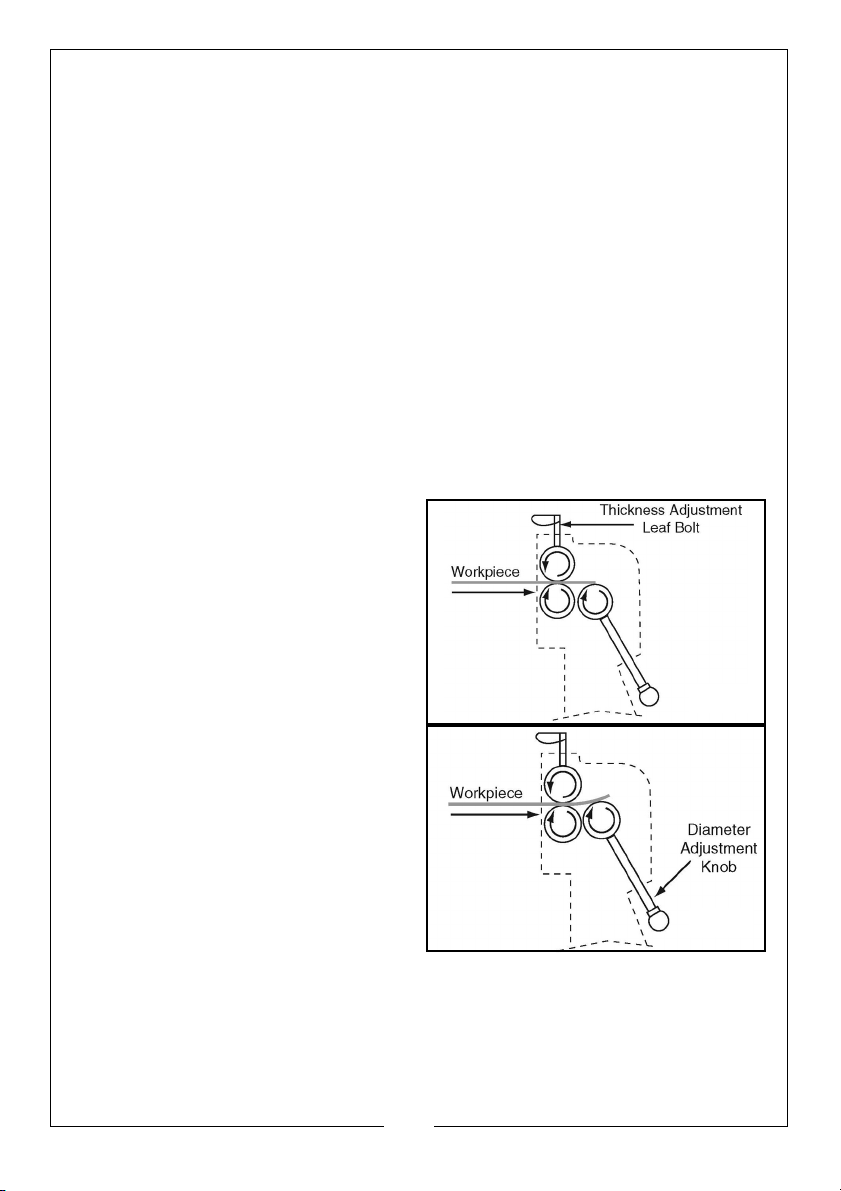
CREATING CURVES
Fig. 12
Fig. 13
Your sheet metal machine can easily create constant radius curves in sheet
metal up to 1 mm in thickness (mild steel).
The method of creating a specific radius is a trial and error process. Due to the
many variations among metal workpieces, no single configuration of the
rollers will reproduce the same curve in all materials. We recommend testing
your roller configurations on scrap pieces that are the same dimension and
material as your final workpiece.
TO CREATE A CURVE IN THE WORKPIECE:
1. Use the diameter adjustment knobs to fully lower the rear roller below the
level of the bottom roller, then rotate the thickness adjustment leaf bolts
counterclockwise until the upper roller can be lifted with enough
clearance for the workpiece.
NOTE: Performing multiple passes through the machine with gradual
reductions in the curve radius produces better results than trying to
make the curve in one or two passes.
2. Insert the workpiece between the
upper and lower rollers and just
over the rear roller, as illustrated in
Figure 12, then tighten the
thickness adjustment leaf bolts
down to hold the workpiece
securely. Make sure you tighten
the leaf bolts exactly the same
amount.
3. Use the diameter adjustment
knobs to raise the rear roller, then
use the hand crank to pass the
workpiece through the machine
(see the illustrations in Figure 13-
14).
NOTE: For good results, make the
first bend about 25% of the
the final radius, then slightly
increase the bend by 25%
with each successive pass
until the final radius has been reached.
11
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 12
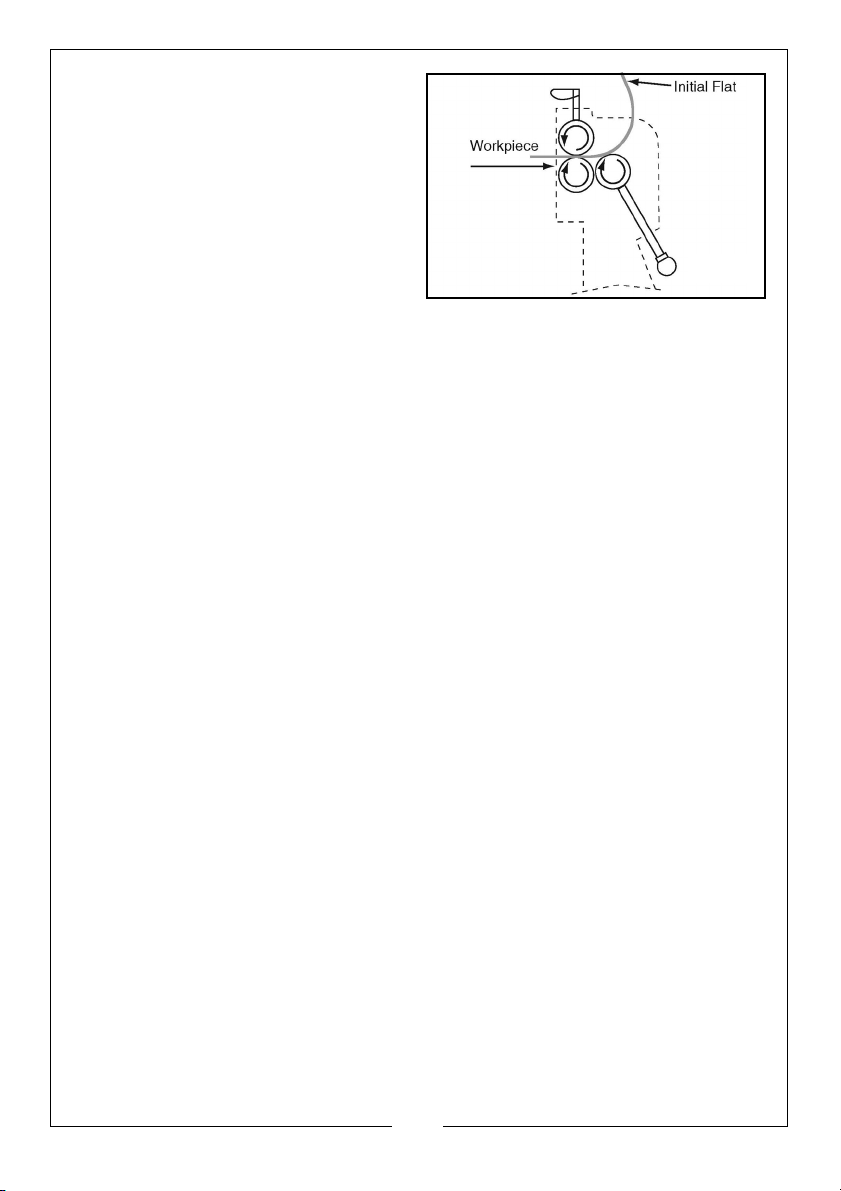
NOTE: If your workpiece has an
Fig. 14
undesired initial flat, as
illustrated in Figure 14, you
can remove it by flipping the
workpiece around and pass
it through the front of the
machine so that the initial
flat enters last.
4. Slightly tighten the diameter
adjustment knobs the same
amount, then pass the workpiece
through the rollers again.
NOTE: To make a cone, tighten one adjustment knob more than the other.
5. Repeat Step 4 until you have produced the desired curve.
CREATING CYLINDERS
If you know the diameter of the cylinder you want to create, use the formula
below to calculate the length of material needed.
C=πD
C = Circumference (Length of Material Needed)
π = Pi (Approximately 3.142)
D = Diameter
Example: Suppose you want to create a 150 mm diameter cylinder. You would
use the above formula as follows:
C = πD
C = (3.142) x 150 mm
C = 471.3 mm
The result of 471.3 mm indicates that you need to start with a piece of sheet
metal that is approximately 471.3 mm in length in order to create a 150 mm
diameter cylinder.
12
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 13
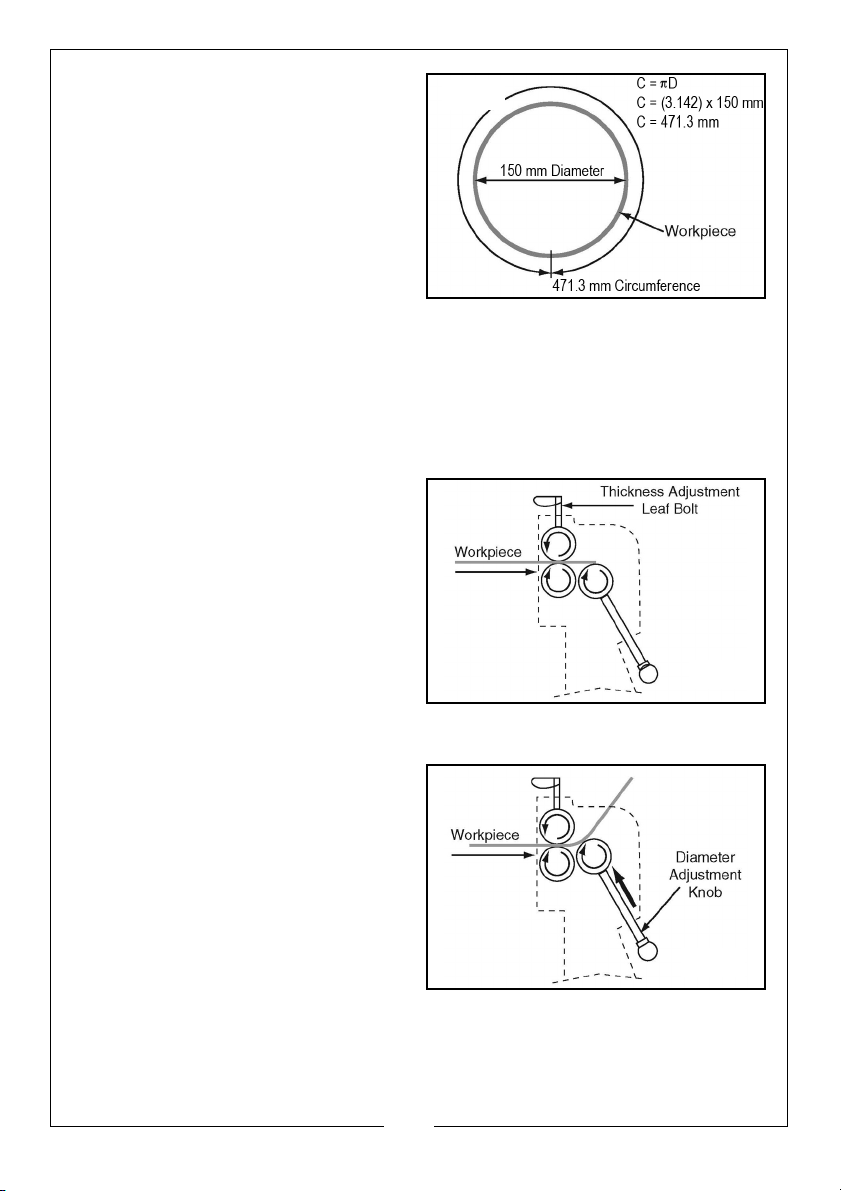
Fig. 15
Fig. 16
Fig. 17
You can use the slip roll to create a
bend with the correct radius so that
the two ends meet, forming a 150
mm diameter cylinder (Figure 15).
NOTE: Performing multiple passes
through the machine with
gradual reductions in the
curve radius produces better
results than trying to make
the curve in one or two
passes.
TO CREATE A CYLINDER:
1. Use the diameter adjustment knobs to fully lower the rear roller below the
level of the bottom roller, then rotate the thickness adjustment leaf bolts
counterclockwise until the upper roller can be lifted with enough
clearance for the workpiece.
2. Insert the workpiece between the
upper and lower rollers and just
over the rear roller, as illustrated in
Figure 16, then snug the thickness
adjustment leaf bolts down to
secure the workpiece. Make sure
you tighten the leaf bolts the
same amount.
3. Turn the hand crank clockwise to
feed the workpiece through the
machine until it is approximately
half way through the upper and lower rollers.
4. Turn the diameter adjustment
knobs clockwise knobs to lift the
rear roller until the desired radius
bend is reached, as illustrated in
Figure 17. Make sure to turn the
knobs equal amounts so the rear
roller is always parallel with the
other rollers. Failure to do so will
create a larger radius on one end
than the other, resulting in a cone
shape.
NOTE: Always err on the side of making the radius too large rather than too
small. It is easy to decrease the radius but very difficult to increase the
radius later.
13
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 14
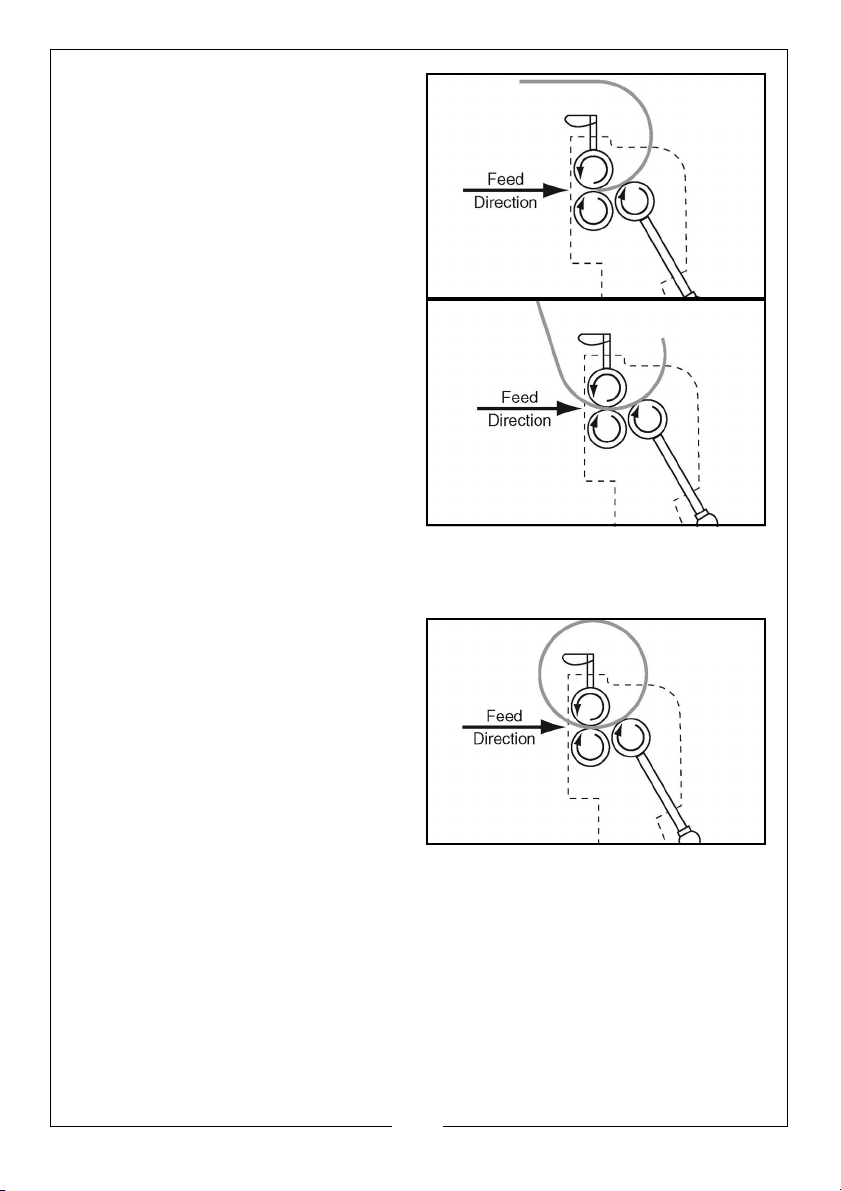
5. Turn the hand crank to process
Fig. 18
Fig. 19
Fig. 20
the material through the slip
rollers. Continue turning until the
workpiece is completely through
the upper and lower rollers, as
illustrated in Figure 18.
6. Rotate the workpiece 180°, insert
the curved end into the rollers,
then process it through the
machine, as illustrated in Figure
19.
7. Reduce the radius of the curve by
raising the rear roller, then repeat
Steps 4-7 until you have produced
the desired cylinder (see the
illustration in Figure 20).
• If the ends of the cylinder do not meet, lift the rear roller equally at both
ends, then process the entire cylinder through the slip roller again.
Repeat as necessary.
• If the ends of the cylinder
overlap, remove the cylinder as
described in “Removing the
workpiece from the rollers” on
page 15. Then, either attempt
to increase the radius by
manually bending it, or scrap
the workpiece and start this
procedure again with a new
blank.
8. When the cylinder is complete,
refer to “Removing the workpiece from the rollers” on page 15 for detailed
instructions on removing the cylinder from the top roller.
14
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 15
REMOVING THE WORKPIECE FROM T H E R OLLERS
Fig. 21
Fig. 22
Fig. 23
TO REMOVE THE WORKPIECE FROM THE TOP ROLLER:
1. Rotate the thickness leaf bolts
anticlockwise until they no longer
apply pressure to the top roller.
CAUTION: THE SHARP EDGES OF
SHEET METAL CAN QUICKLY
CUT YOUR HANDS. ALWAYS USE
CAUTION AND HEAVY LEATHER
GLOVES WHEN HANDLING
SHEET METAL.
2. Protect your hands from the sharp
edges of the workpiece, then
grasp the top roller and use
moderate force to pull it forward,
as shown in Figure 22.
3. Remove the workpiece, slide the
top roller back into place, then
secure the roller by rotate the
thickness leaf bolts clockwise to
apply the required pressure to the
top roller.
BENDING WIRE
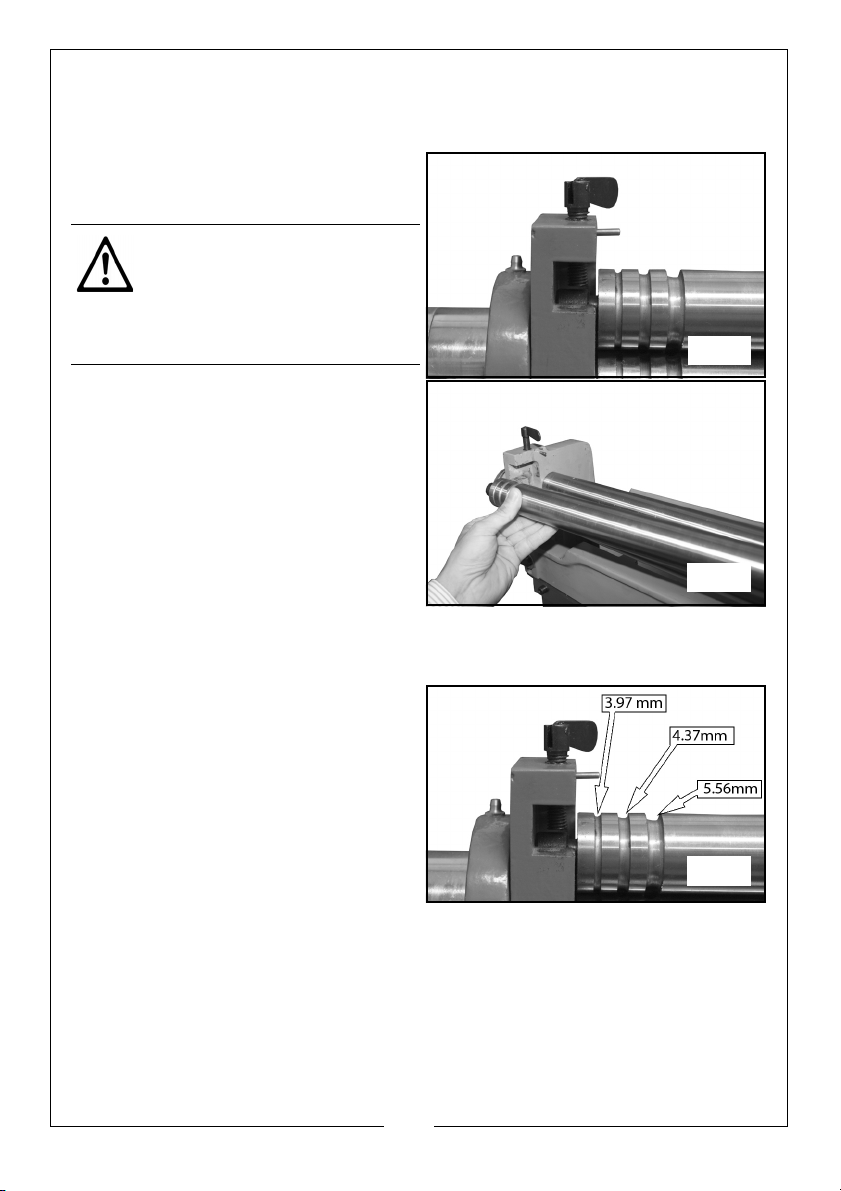
Your sheet metal machine can bend
wires, rods, and small-diameter
tubing with diameters of 3.97 mm,
4.37 mm and 5.56 mm (see Figure 23).
To ensure even pressure on the
material, place the workpiece in the
smallest possible groove on the
rollers.
Process the material through the
machine in the same manner
described on the previous pages for sheet metal.
NOTE: The wire grooves can also be used when rolling sheet metal that has a
wire bead on the side.
15
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 16
OPERATING - BRAKE
Fig. 24
Fig. 25
Fig. 26
BRAKE OVERVIEW
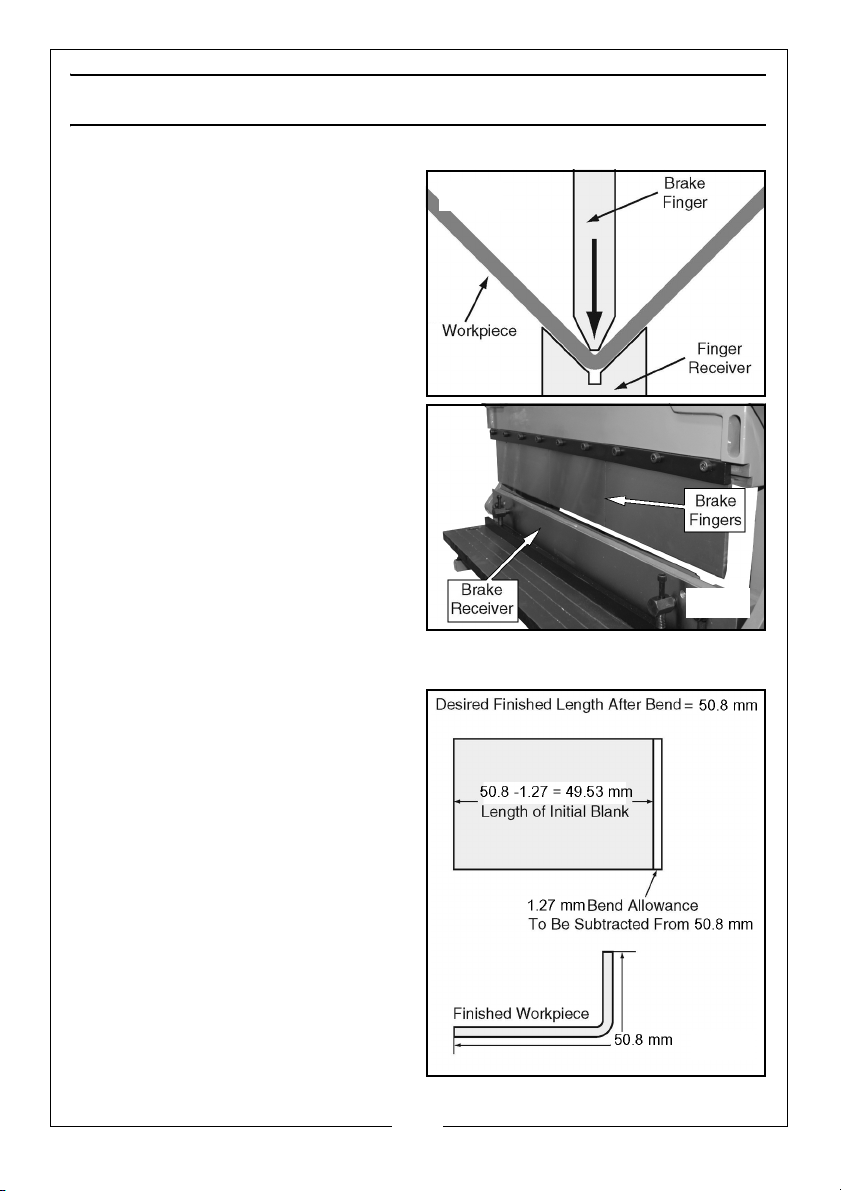
The brake of the SBR760 is used to
make bends of 0°-90° in sheet metal
up to 1 mm in thickness and 760 mm
in width. When you use the hand
crank, the brake fingers force the
workpiece into the groove of the
finger receiver to make the desired
bend (see Figures 24-25).
BEND ALLOWANCE
When metal is bent, the outside
overall dimension increases from its
original length-this amount is called
the bend allowance. A typical bend
allowance for a 90° bend in a 1 mm
mild steel workpiece is approximately
1.27 mm. That means you need to
start with a workpiece that is
approximately 1.27 mm shorter than
the desired outside length of the
finished workpiece, as illustrated in the example of Figure 26.
Calculating the bend allowance for
your operation requires many
variables, such as metal thickness,
type of material, radius of the bend,
etc. Detailed information for
calculating the bend allowance can
be found in metalworking handbooks
and on the internet.
An easy way to find the correct
dimension of your initial blank is to
measure a piece of scrap of the
same material as the workpiece,
make the bend, then measure the
piece again. The difference between
the two measurements is the bend
allowance, which you subtract from
the dimension of the workpiece
blank before the bend.
16
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 17
BENDING SHEET METAL
Fig. 27
Fig. 28
Tip: To reduce the chance of scoring your workpiece when using the brake,
always keep the fingers and receivers clean and lubricated (refer to page 21
for detailed instructions), and free of burrs or other blemishes. Also, apply a
strip of sturdy tape along the top and bottom of the bend line.
WARNING: THE BRAKE FINGERS ON THIS MACHINE PRESENTS A PINCHING
HAZARD. MAKE SURE NO BODY PART OR CLOTHING IS NEAR THE AREA
WHERE METAL BENDING OCCURS. FAILURE TO FOLLOW THIS WARNING
MAY RESULT IN SEVERE PERSONAL INJURY.
TO BEND SHEET METAL:
1. Mark a line along the width of the workpiece where the bend is to take
place.
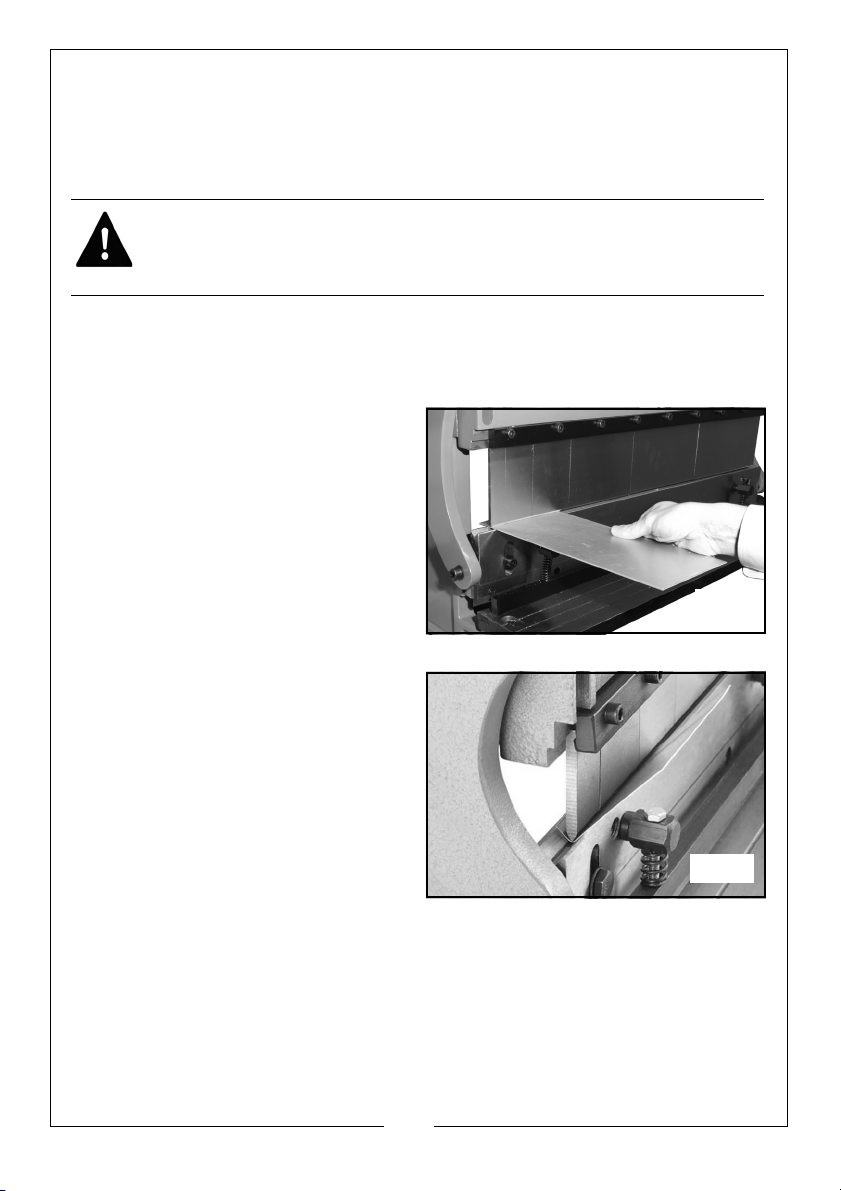
2. Use the hand crank to lower the
finger receiver until you can
position the workpiece
underneath the fingers with the
bend line aligned with the tips, as
shown in Figure 27.
NOTE: When performing the same
bending operation on
multiple parts, use the rear
work stop to save time
positioning the workpieces.
3. While holding the workpiece
steady, use the hand crank to
raise the finger receiver to
perform the desired bend (see
Figure 28 for an example), then
lower the receiver and remove
the workpiece.
17
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 18
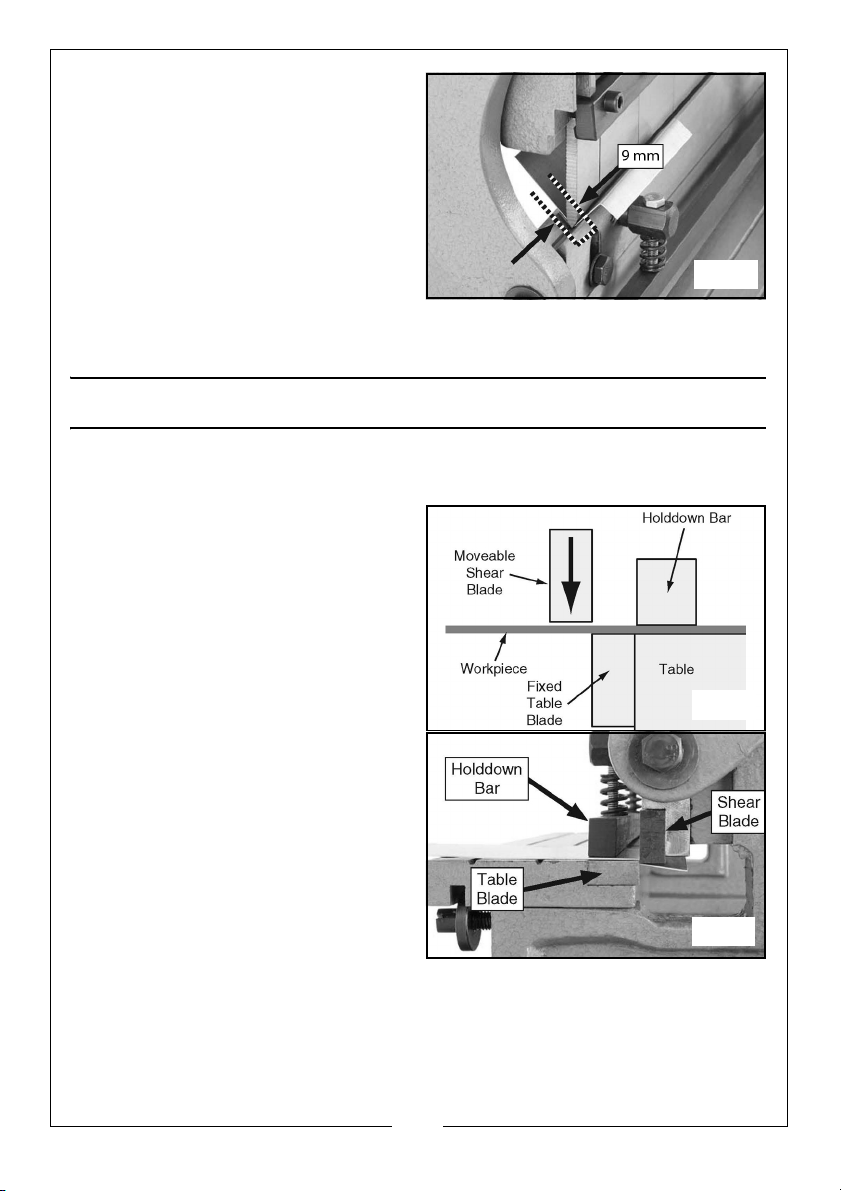
4. If a reverse bend is required, re-
Fig. 29
Fig. 30
Fig. 31
install the workpiece upsidedown, as shown in Figure 29, and
repeat Steps 2-3. The minimum
reverse bend possible is 9 mm.
NOTE: When performing a pan and
box bending operation,
loosen the cap screws on
the brake finger gib and
configure the fingers for your
operation. Remove the
fingers you do not need.
OPERATING - SHEARING
SHEARING OVERVIEW
The SBR760 has a set of reversible
blades that shear mild steel up to 1
mm in thickness and 760 mm in width.
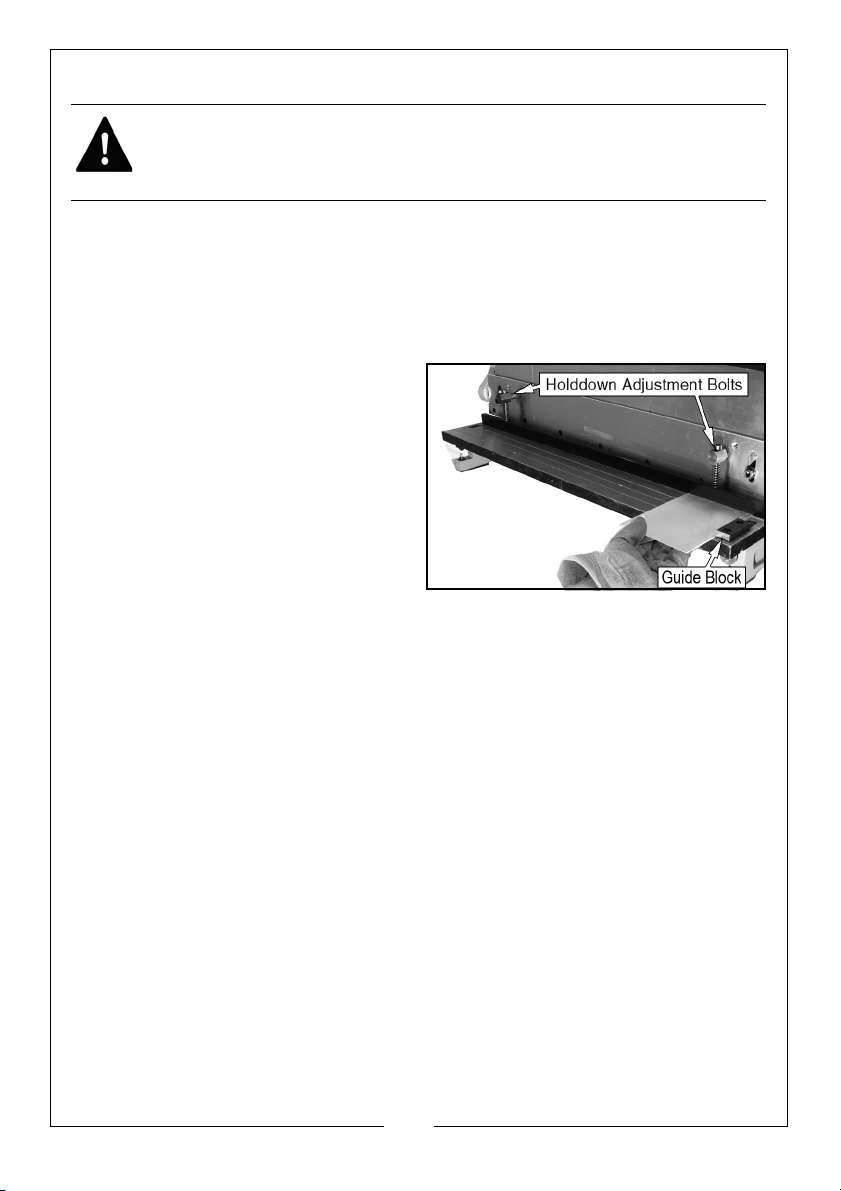
When you use the hand crank to
perform a shear, the upper movable
blade is lowered past the fixed table
blade, creating a shearing action
(see Figures 30-31). For repetitive cuts,
use the adjustable rear work stop.
18
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 19
CUTTING SHEET METAL
Fig. 32
WARNING: THE SHEARING BLADES ON THIS MACHINE PRESENT A
HAZARD. MAKE SURE NO BODY PART OR CLOTHING IS NEAR THE AREA
WHERE METAL SHEARING OCCURS. FAILURE TO FOLLOW THIS WARNING
MAY RESULT IN SEVERE PERSONAL INJURY.
To cut sheet metal:
1. Mark the cut line across the width of the workpiece.
2. Make sure the gap between the shearing blades is correct for the
workpiece material (refer to “Shearing Blade Gap Adjustment” on page 25
for detailed instructions).
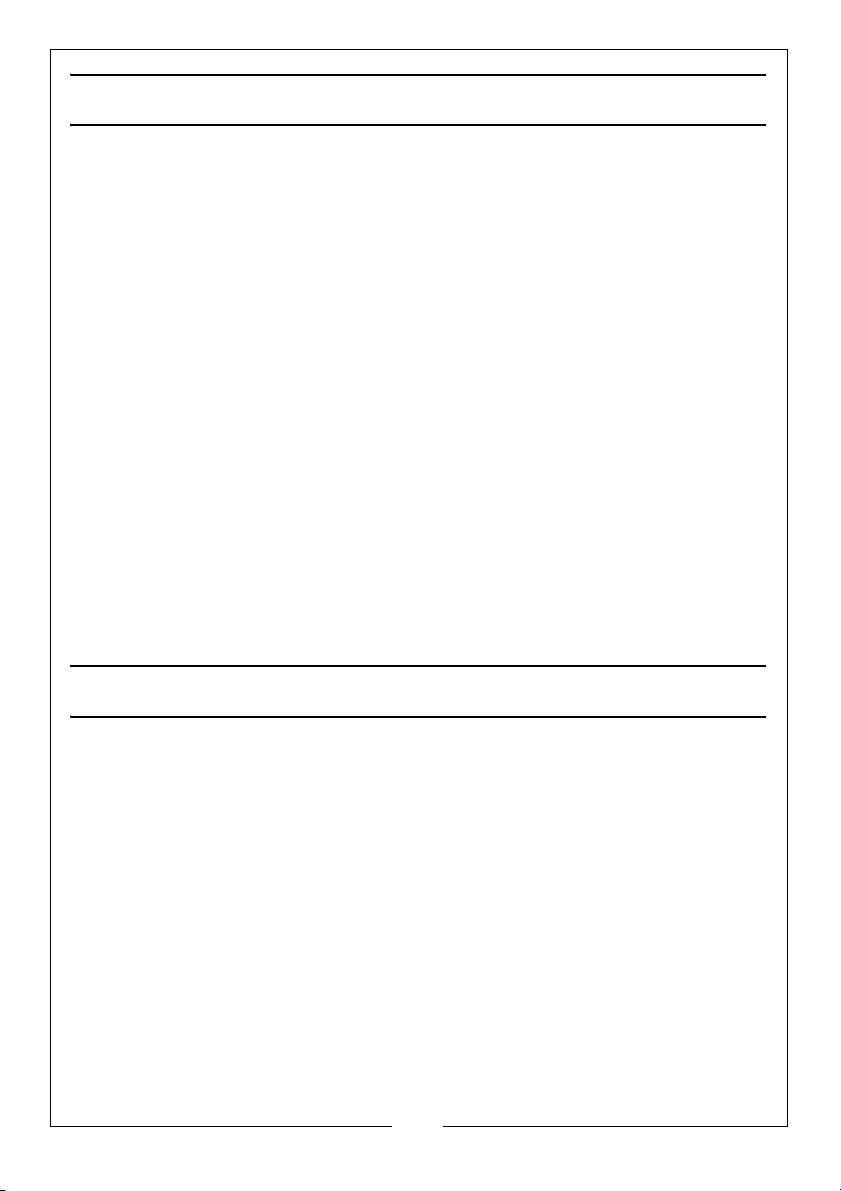
3. Position the workpiece up against
the guide block on the right side
of the table, then align the cut
mark with the upper shear blade,
as shown in Figure 32.
NOTE: The shearing action begins
on the right side of the
workpiece and moves to the
left.
NOTE: If you need to adjust the gap
between the shearing blades to accommodate your workpiece,
refer to the “Shearing Blade Gap Adjustment” on page 25 for
detailed instructions.
NOTE: If you are using the rear work stop, adjust the stop so that at least one
square edge of the workpiece is against it.
4. Use the hold down adjustment bolts to adjust the holddown bar so that it
firmly holds the workpiece in place without marking or denting it.
5. Keeping all body parts away from the blades, rotate the hand crank with
an even and steady pressure to complete the cut.
MATERIAL THICKNESS
The SBR760 is designed to bend and shear mild steel sheet metal up to 1 mm in
thickness.
19
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 20
MAINTENANCE
SCHEDULE
For optimum performance from your machine, follow this maintenance
schedule and refer to any specific instructions given in this section.
DAILY MAINTENANCE:
• Clean the machine.
• Tighten loose mounting bolts.
• Check/replace damaged rollers.
• Check/replace cracked or damaged brake fingers or receiver.
• Sharpen/replace dull or nicked shearing blades.
• Any other unsafe condition.
MONTHLY MAINTENANCE:
• Lubricate the gears and hand crank bushings.
SEMI-ANNUAL MAINTENANCE:
• Lubricate the roller bushings.
CLEANING
Cleaning the SBR760 is relatively easy. Use cloth and degreasing spirits to wipe
down the machine.
LUBRICATION
Keep your SBR760 properly lubricated to help ensure long life and smooth
operation of the machine.
20
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 21
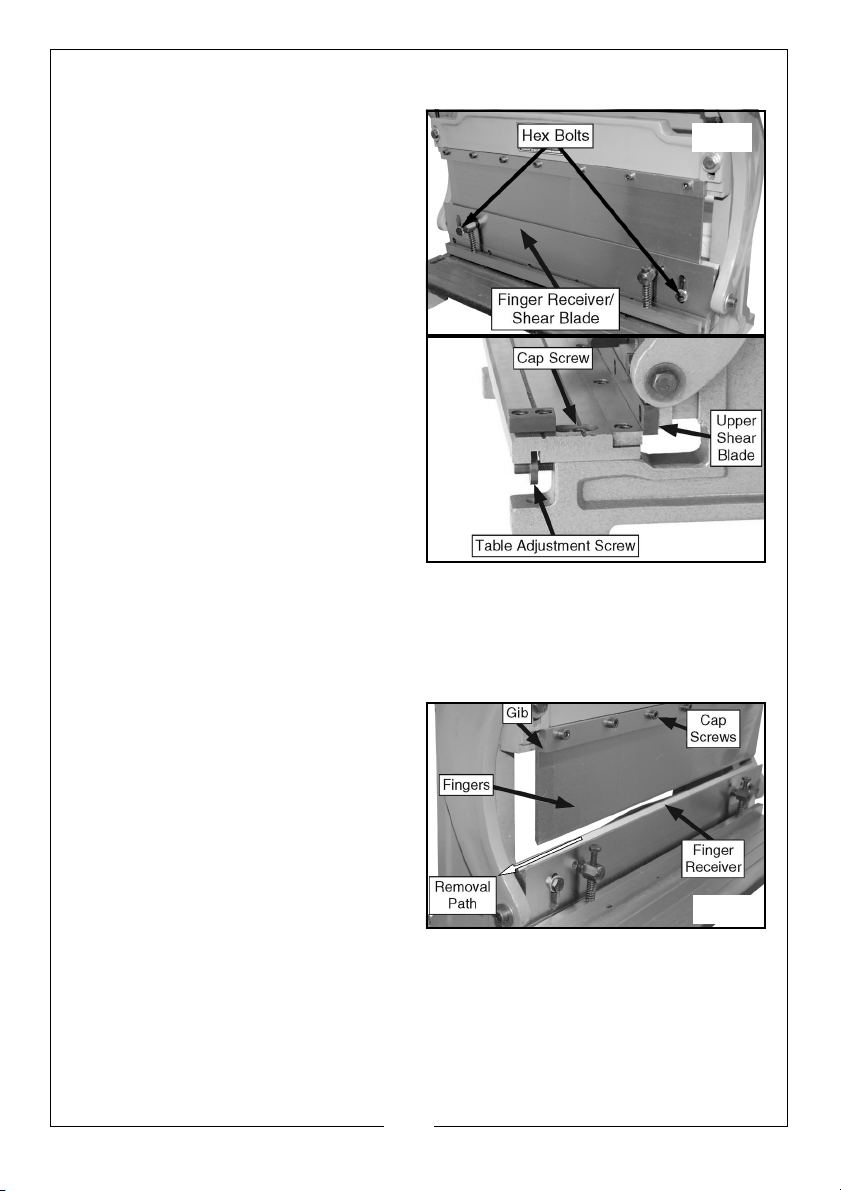
CLEAN THE MACHINE FINGERS
Fig. 33
Fig. 34
Fig. 35
1. Loosen the two hex bolts securing
the finger receiver/upper shear
blade to the frame (see Figure
33).
2. Move the table back until the
upper shear blade can pass
down behind the table blade by
loosening the two cap screws
securing the shear table to the
frame and rotating the table
adjustment screws
counterclockwise (see Figure 44).
NOTE: Operational adjustment of
the shearing blades is
covered in the “Shearing
Blade Gap Adjustment” on page 25.
3. Make sure the finger receiver and upper shear blade move up and down
smoothly, retighten the hex bolts just until they are snug, then back them
off approximately ¼ turn.
4. Use the hand crank to position the
brake finger receiver close to the
brake fingers, as shown in Figure
35.
5. Loosen the gib cap screws to
release the fingers, then remove
the fingers from the side of the
finger receiver, as shown in Figure
35.
6. Use cloth and a degreaser to
remove the storage grease from the fingers, gib, and receiver. Thoroughly
dry the parts, then apply a thin coat of an anti-rust lubricant to all the parts.
21
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 22
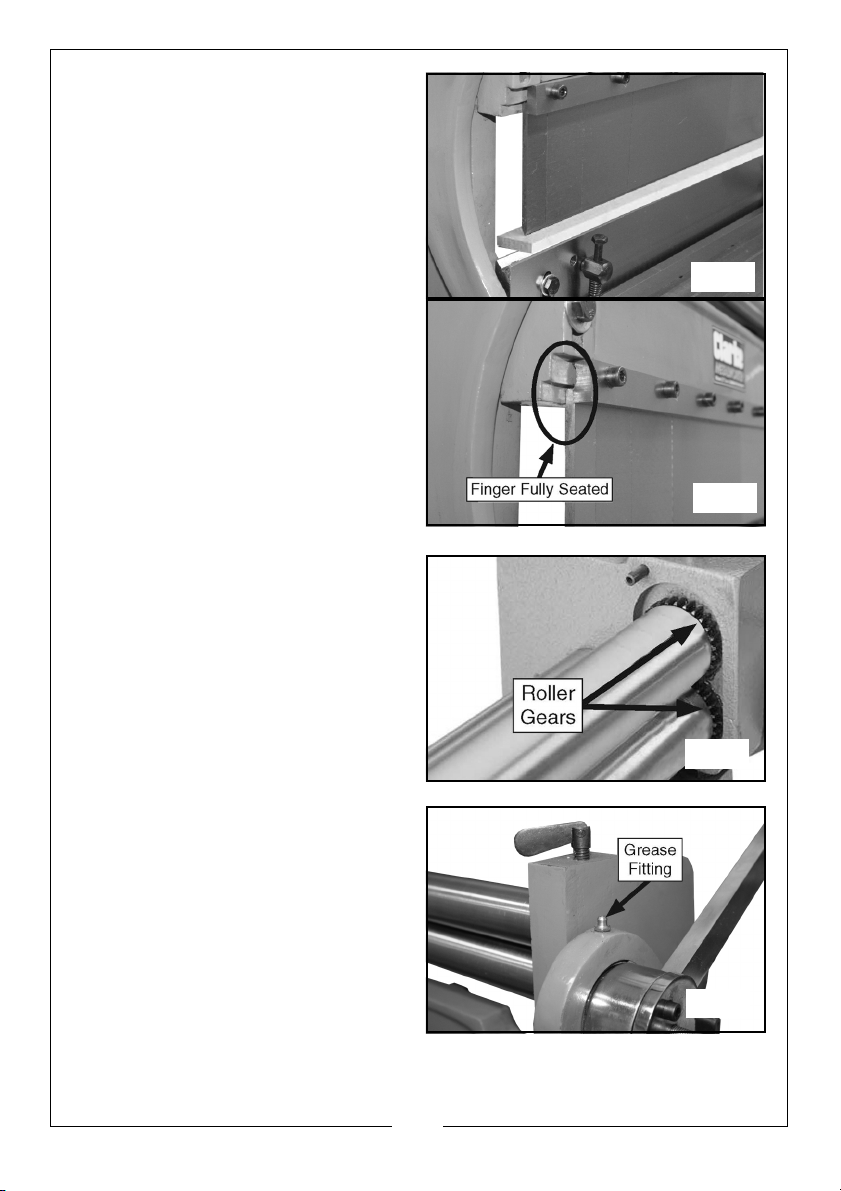
7. Place a thin piece of wood on the
Fig. 36
Fig. 37
Fig. 38
Fig. 39
finger receiver, as shown in Figure
36, then reinstall the fingers so that
they rest on the wood. Make sure
the tops of the fingers are
between the gib and the casting.
NOTE: Install the widest finger to the
right, then repeat with each
smaller finger.
8. Make sure the fingers are slightly
loose between the gib and the
casting, then use the hand crank
to raise the receiver to fully seat
the fingers up against the casting
behind the gib, as shown in Figure
37.
9. Re-tighten all of the gib cap
screws.
GEARS
Clean away grease and built-up
grime from the top and bottom roller
gear teeth, as shown in Figure 38,
with a stiff brush and degreasing
spirits.
When dry, apply a small amount of
grease to the teeth, then use the
hand crank to rotate the rollers and
distribute the lubricant.
HAND CRANK BUSHINGS
Wipe off the grease fittings next to
each hand crank hub (see Figure 39),
then use a grease gun to add a small
amount of multi-purpose grease to
the hand crank bushings.
22
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 23
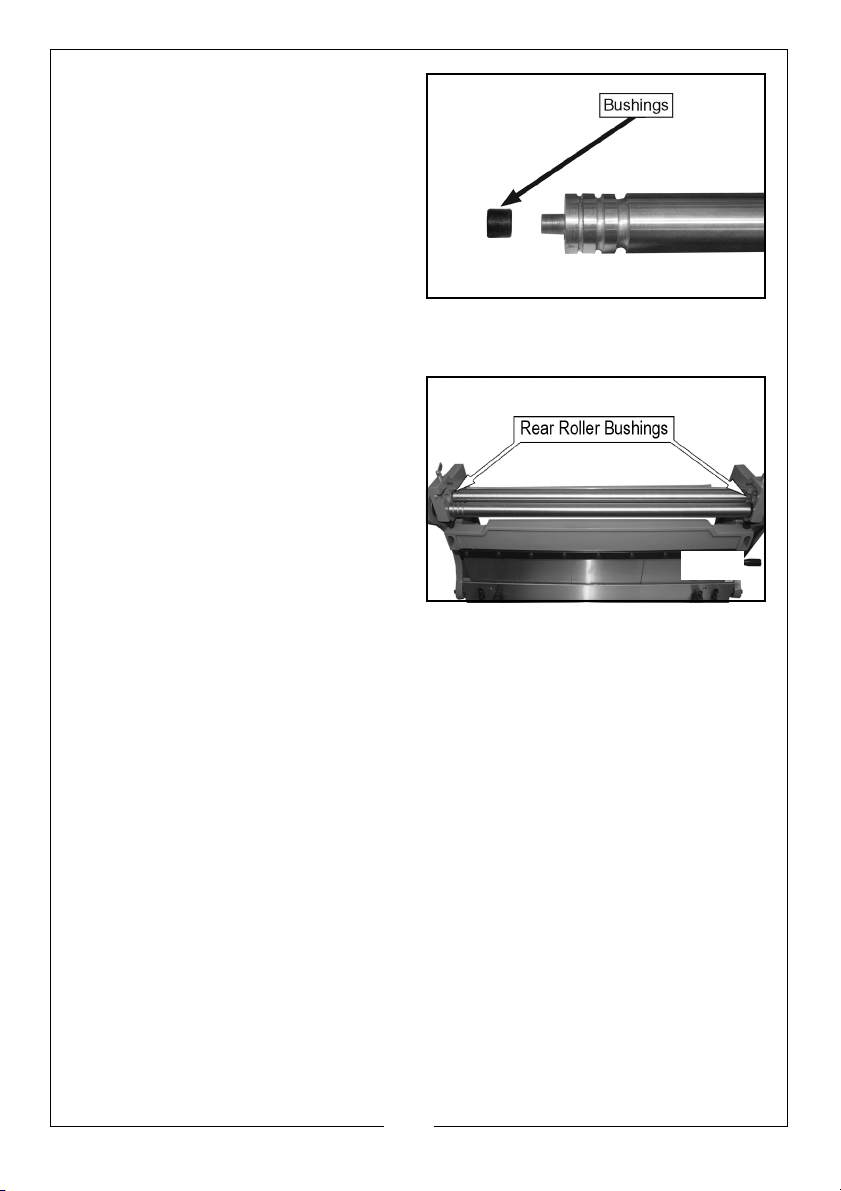
ROLLER BUSHINGS
Fig. 40
Fig. 41
1. Remove the top roller from the
machine, then remove the
bushings from the ends of the
roller (see Figure 40).
2. Use a shop rag and degreasing
spirits to clean the bushings and
the ends of the roller,
3. Apply a thin coat of multi-purpose
grease to the roller ends
4. Re-install the bushings.
5. Use a stiff brush and degreasing
spirits to clean the rear roller
bushings (see Figure 41),
6. Apply a small amount of multipurpose grease to them.
7. Re-install the top roller and close
the cover.
23
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 24
SERVICE
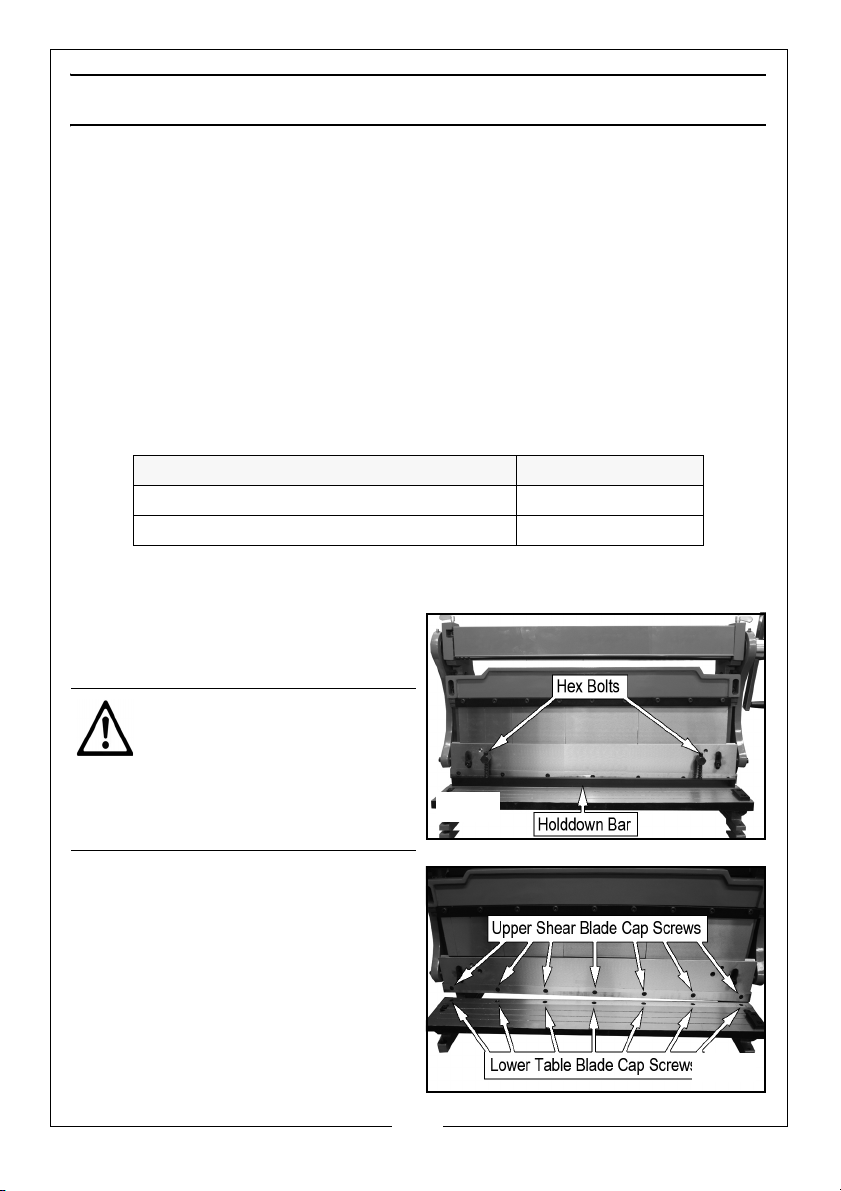
Fig. 42
Fig. 43
SHEARING BLADE REVERSAL/REPLACEMENT
The shearing blades are reversible, so when the first cutting edge becomes
dull, the blades can be rotated to use the second cutting edge.
When both cutting edges of the blade become dull, use wet grinding
techniques for SK-4 metal or better to sharpen the cutting face of the blade.
The upper shearing blade uses a 5° relief edge and the lower table blade
does not. However, if you are not comfortable performing the sharpening
procedure or do not have access to a professional sharpening service,
replacement blades are available through the Clarke spares department.
Tools Needed
Tools Needed Qty
Wrench or Socket 10 mm 1
Hex Wrench 5mm 1
TO REVERSE OR REPLACE THE SHEARING BLADES:
1. Remove the hex bolts and springs
that secure the shear holddown
bar (see Figure 42).
CAUTION: THE SHEARING
BLADES ARE SHARP AND CAN
QUICKLY CUT YOUR HANDS.
ALWAYS WEAR HEAVY LEATHER
GLOVES WHEN HANDLING THE
SHEARING BLADES TO AVOID
THIS CUTTING HAZARD.
2. Remove the six cap screws that
secure the blade, then carefully
remove it from the machine (see
Figure 43).
Tip: When removing or installing the
upper shear blade, remove the cap
screw at one end, then insert a small
hex wrench or similar tool through the
24
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 25
hole to keep the blade in place as you remove the rest of the cap screws.
3. Inspect the blade cutting edge that was in use, for wear, nicks, or burrs.
• If the cutting edge shows wear or nicks and the other cutting edge
has not been used, rotate the blade and re-install it.
• If both cutting edges are worn or nicked, either properly sharpen the
cutting face or replace the blade.
4. Re-install the holddown bar, then check that the shearing blade gap
adjustment is correct as instructed in “Shearing Blade Gap Adjustment”
below.
SHEARING BLADE GAP ADJUSTMENT
The shearing blade gap adjustment determines the accuracy of the cut.
Follow the procedures below to make sure this adjustment is correct for the
workpiece material being processed.
WARNING: THE SHEARING BLADES ON THIS MACHINE PRESENTS AN
HAZARD. MAKE SURE NO BODY PART OR CLOTHING IS NEAR THE AREA
WHERE METAL SHEARING OCCURS. FAILURE TO FOLLOW THIS WARNING
MAY RESULT IN SEVERE PERSONAL INJURY.
PERFORMING THE SHEAR TEST
1. While keeping your fingers clear of the shear blades, shear a piece of scrap
material that is the same as your workpiece along the full length of the
blade, then inspect the cut.
• If the machine correctly cuts to your satisfaction along the entire
length of the blades, no adjustments are necessary.
• If the cut is clean at one end and not the other, perform the
following ADJUSTING THE SHEAR TABLE procedure on page 26.
• If the condition of the cut on the ends is different from the cut in the
middle, perform the following “Adjusting the Blade Bow” on
page 26.
25
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 26
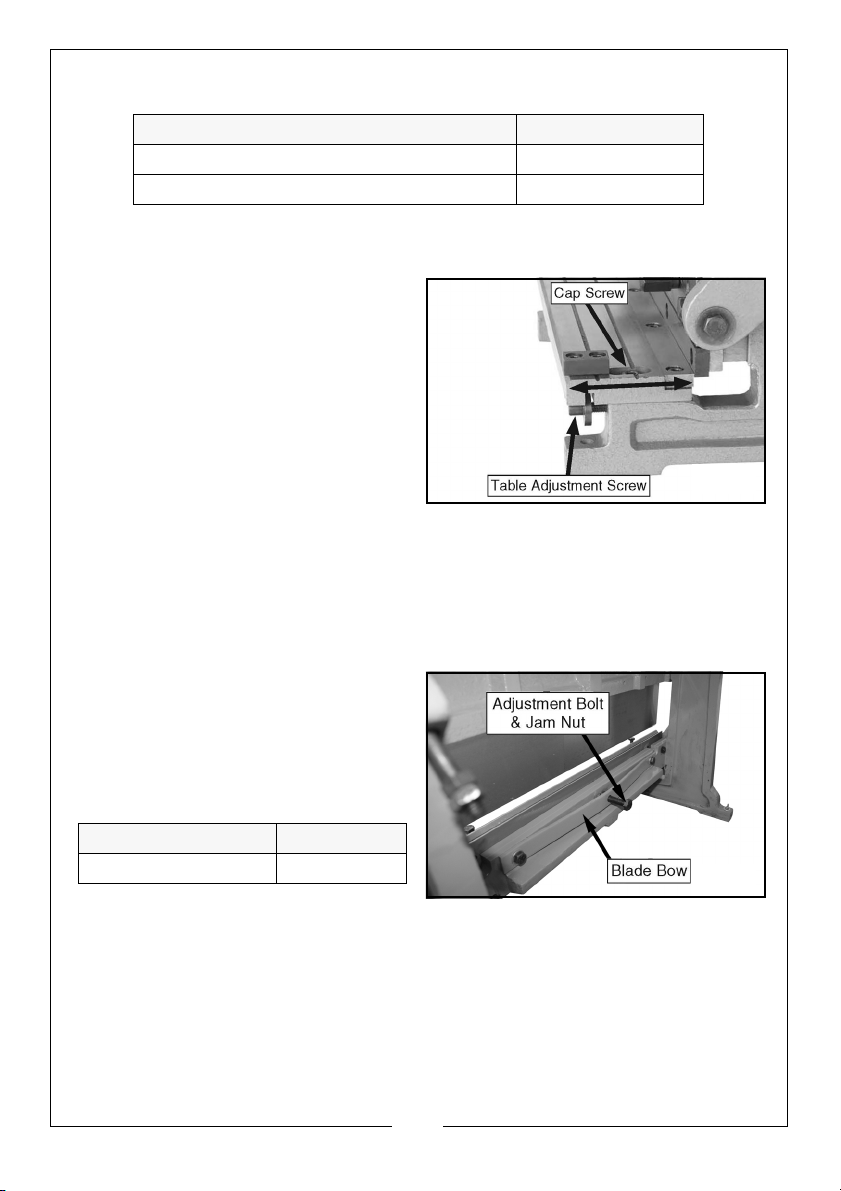
ADJUSTING THE SHEAR TABLE.
Fig. 44
Fig. 45
Tools Needed Qty
Hex Wrench 6mm 1
Standard Screwdriver #2 1
TO ADJUST THE BLADE GAP BY MOVING THE TABLE:
1. Loosen the cap screws on either
end of the shear table that secure
it to the machine (see Figure 44).
2. Evenly rotate the table
adjustment screws to adjust the
position of the shearing table until
the blade gap is even, then retighten the cap screws to secure
the table in place.
NOTE: Rotating the table
adjustment screws clockwise moves the table toward the upper
shear blade.
3. Perform the previous shear test.
4. If necessary, repeat Steps 1-3 until you are satisfied with the shear test cut.
ADJUSTING THE BLADE BOW
The adjustment bolt of the blade
bow is used to remove any slight bow
in the cast iron cross beam that the
brake finger receiver and upper
shear blade are attached to (see
Figure 45).
Tools Needed Qty
Wrench 14mm 2
26
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 27
TO ADJUST THE BLADE GAP WITH THE BLADE BOW:
1. Hold the adjustment bolt still, then turn the jam nut to adjust the center of
the cross beam in or out (see Figure 48).
• If the shear test cut was clean on the ends of the shear table but not
in the middle, turn the jam nut counterclockwise to force the
adjustment bolt against the cross beam, moving it in toward the
front.
• If the shear test cut was clean in the middle but not on the ends,
rotate the jam nut clockwise to allow the cross beam to move back.
2. Perform the previous shear test.
3. If necessary, repeat Steps 1-2 until you are satisfied with the shear test cut.
BRAKE ALIGNMENT
WARNING: THE BRAKE FINGERS ON THIS MACHINE PRESENTS A PINCHING
HAZARD. MAKE SURE NO BODY PART OR CLOTHING IS NEAR THE AREA
WHERE METAL BENDING OCCURS. FAILURE TO FOLLOW THIS WARNING
MAY RESULT IN SEVERE PERSONAL INJURY.
During the life of your machine, you may need to align the brake fingers with
the finger receiver from side-to-side.
Tools Needed Qty
Hex Wrench 6mm 1
Wrench 16mm 1
Heavy Flat Bar 1
TO ALIGN THE BRAKE:
1. Remove, clean, and de-burr all of the finger tips and the receiver groove,
then inspect the fingers and receiver for any cracks or damage.
• If any of the brake fingers or the receiver are damaged in any way,
DO NOT use the brake until you have replaced these parts with new
ones.
2. Replace the fingers and properly seat them (refer to Steps 8-13 beginning
on page 21 for detailed instructions).
CAUTION: OPERATING THE BRAKE WITH CRACKED OR DAMAGED BRAKE
FINGERS OR RECEIVER COULD CAUSE THESE PARTS TO SHATTER AND FLY
APART, WHICH COULD RESULT IN PERSONAL INJURY.
27
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 28
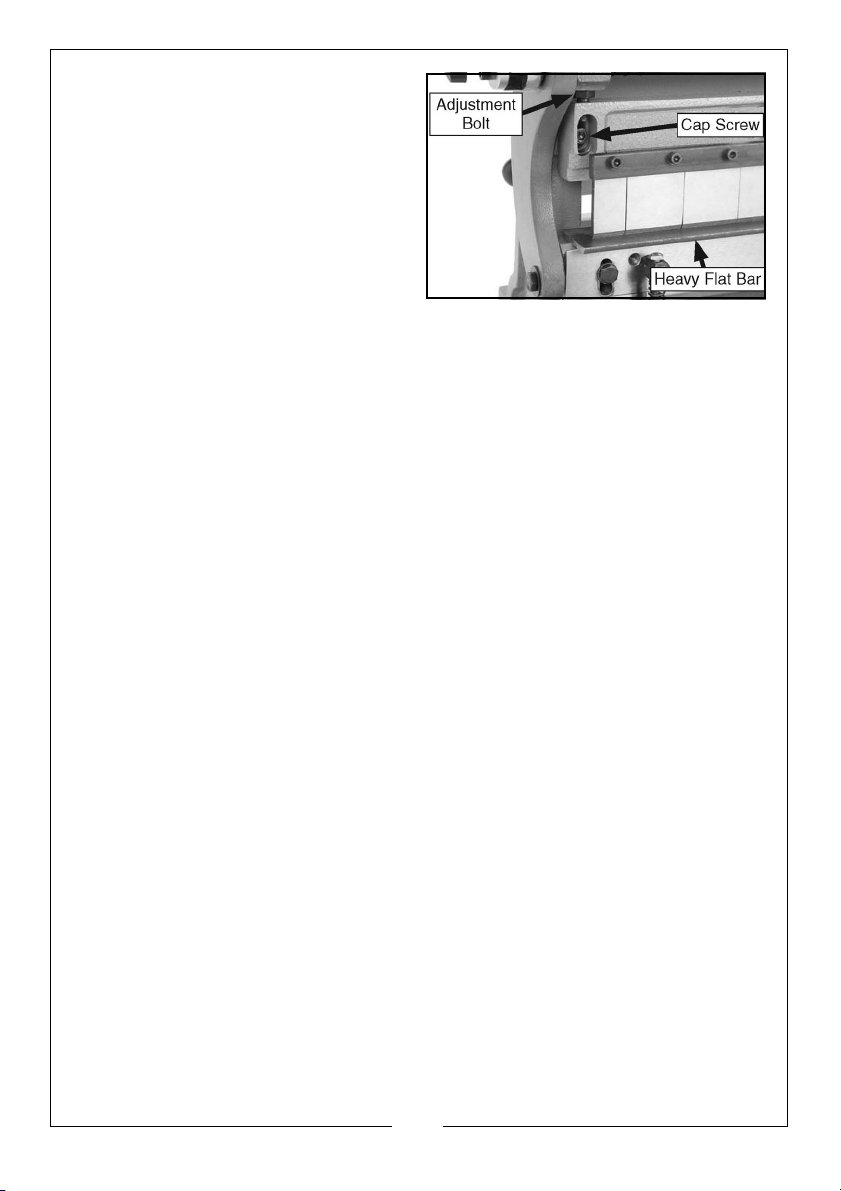
3. Place a piece of heavy flat bar
Fig. 46
stock or a heavy metal ruler
across the finger receiver, as
shown in Figure 46.
4. Lower the brake fingers until one
just rests on the metal bar, as
shown in Figure 46.
5. Starting at one end, visually check
the gap between the brake
fingers and the metal bar.
6. If you find a gap at one end of the brake, loosen the cap screw shown in
Figure 46 on that end, then turn the adjustment bolt counterclockwise until
the gap disappears.
7. Re-tighten the cap screw, remove the metal bar and use the hand crank
to cycle the machine 2-3 times.
8. Repeat Steps 3-7 until the brake fingers rest evenly on the metal bar along
its entire length.
28
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 29
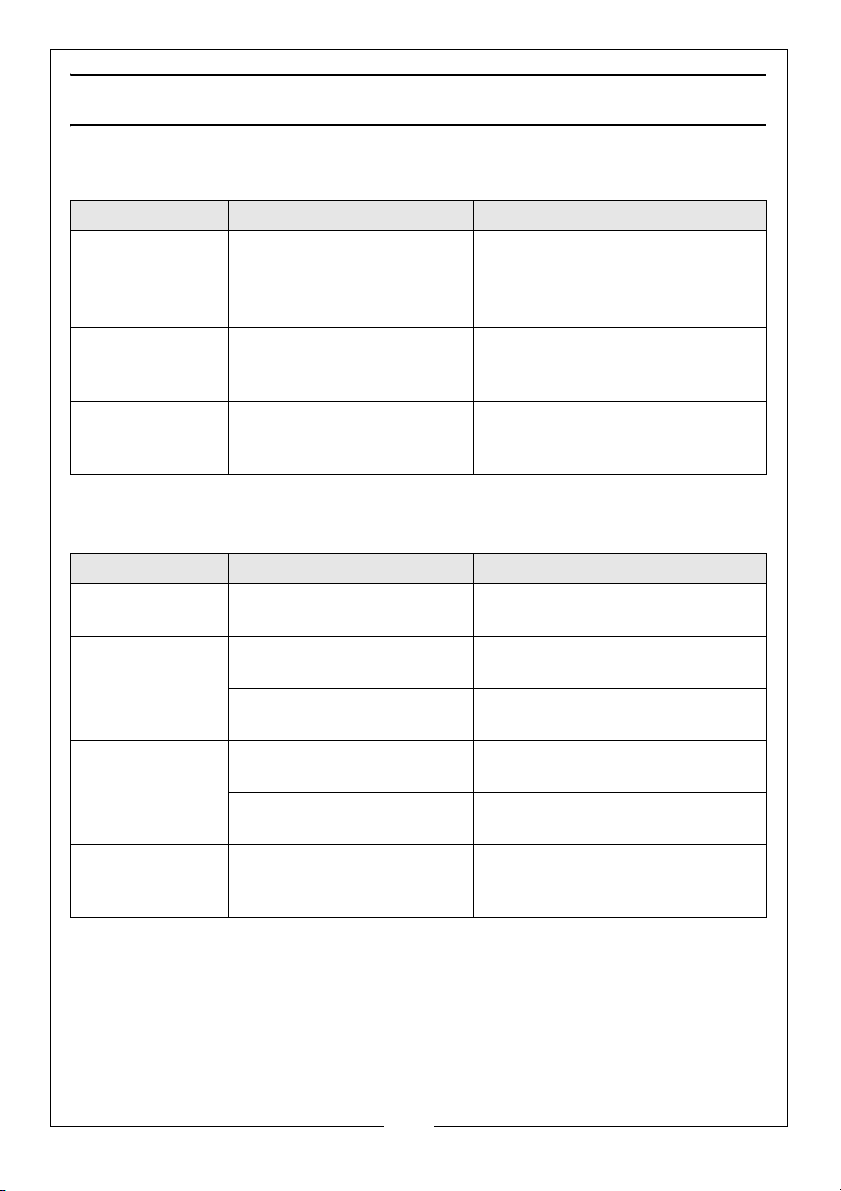
TROUBLESHOOTING
Slip Roll Operation
PROBLEM CAUSE SOLUTION
Slip roll creates
cones when trying
to make a
cylinder.
Creases or
wrinkles in the
workpiece.
Workpiece is
pitted or
scratched.
Top and rear rollers not
parallel.
Excessive pressure applied
when rolling.
Workpiece or rollers are dirty
or damaged.
Use the diameter adjustment knobs
to make the rollers parallel.
Reduce the radius and perform the
bend in several light passes.
Thoroughly clean the workpiece
and rollers. Polish out any nicks/
burrs in the rollers, or replace them.
Brake Operation
PROBLEM CAUSE SOLUTION
Heavy resistance
during bending.
Bend radius is not
consistent across
workpiece.
Tips of brake
fingers are
chipping or rolling.
Workpiece has
scoring marks.
Machine capacities are
exceeded.
Machine capacities are
exceeded.
Fingers and receiver not
aligned.
Fingers and receiver not
aligned.
Workpiece is too thick. Operate within the listed capacities
Fingers or receiver scratched Polish out scratches, and apply
Operate within the listed capacities
of the machine.
Operate within the listed capacities
of the machine.
Properly align the fingers and
receiver
Properly align the fingers and
receiver
of the machine.
tape at the bend locations for
further protection
29
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 30
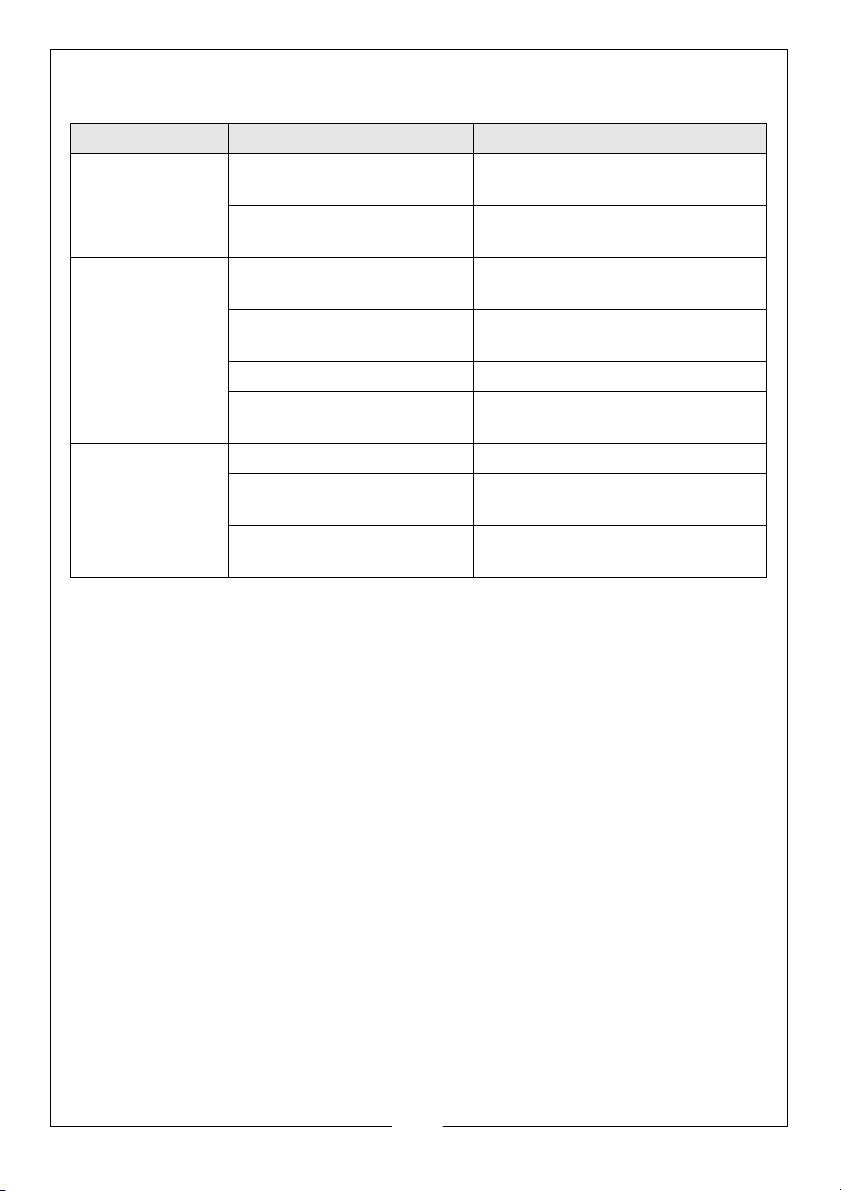
Shear Operation
PROBLEM CAUSE SOLUTION
Machine will not
cut workpiece.
Cuts are not
square.
Poor quality of
cuts with ripping
or tearing.
If this does not solve your problem, please contact the clarke service department.
Cut exceeds machine
capacities
Not enough gap between
blades.
Uneven contact with guide or
work stop.
Blade gap unequal across
length.
Too much bow in blade Properly adjust blade bow
Inadequate holddown
pressure.
Dull blades. Reverse/sharpen/replace blades.
Incorrect blade gap setup. Properly adjust blade gap for
Loose blades. Remove blades, clean thoroughly,
Operate within the listed capacities
of the machine.
Increase blade gap.
Maintain proper contact with guide
and work stop.
Properly adjust blade gap for
material.
Properly adjust holddown pressure.
material.
and re-install.
30
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 31
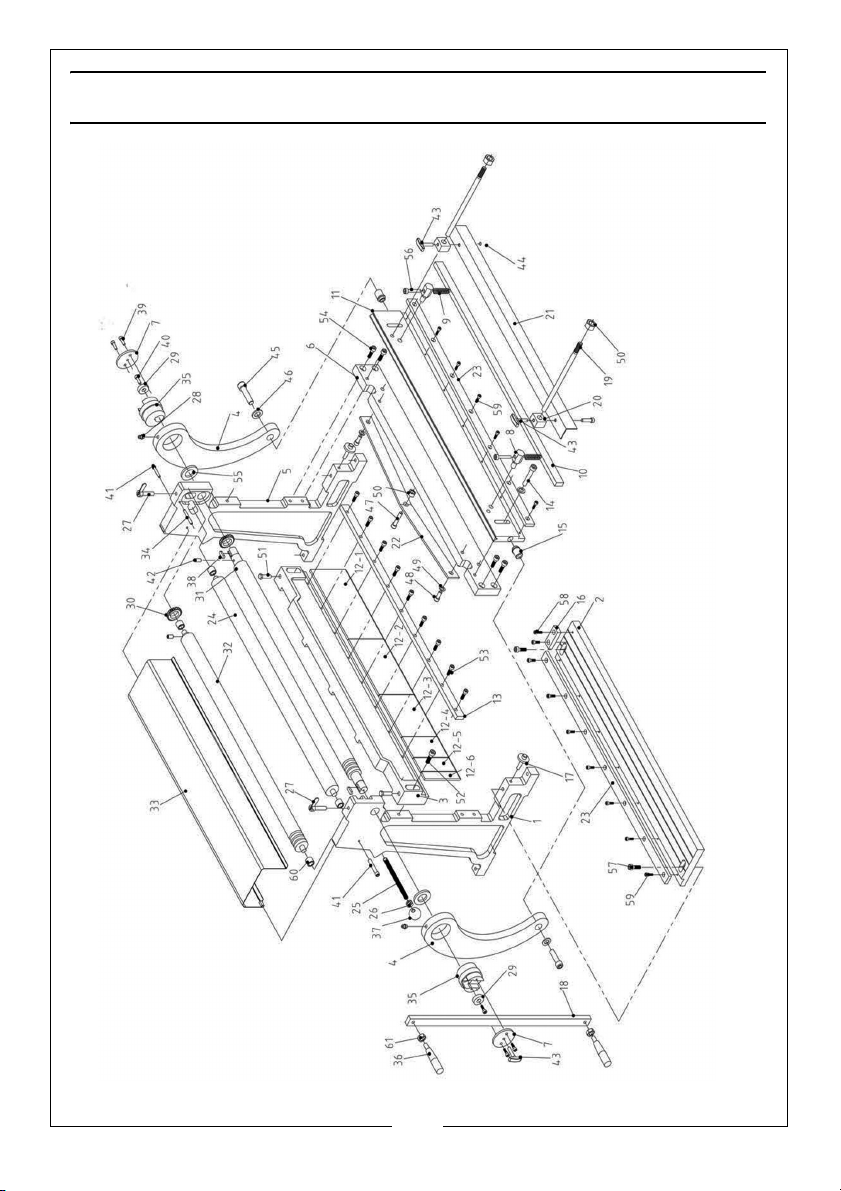
EXPLODED DIAGRAM - PARTS LIST
31
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 32
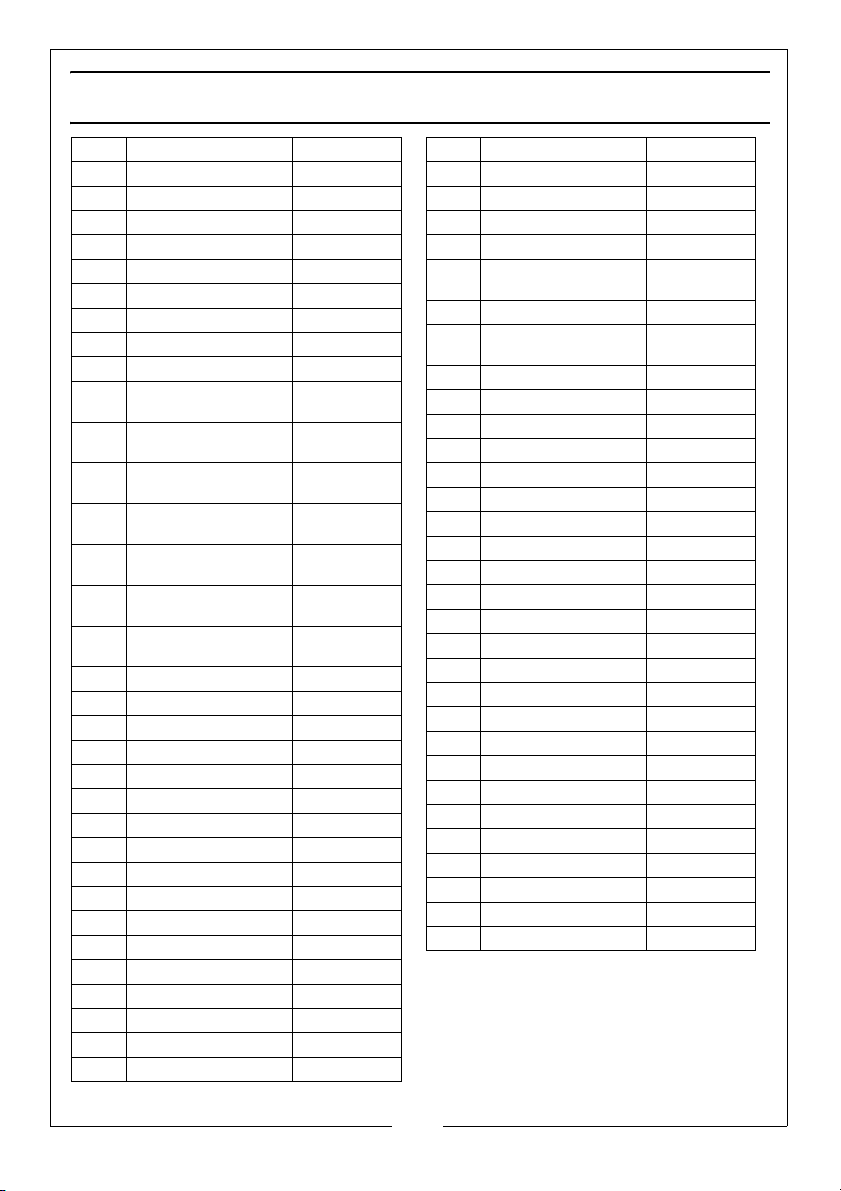
1 LEFT WALL TGSBR76001
2 WORK BENCH TGSBR76002
3 CROSSBEAM TGSBR76003
4 CRANK ARM TGSBR76004
5 RIGHT WALL TGSBR76005
6 REAR FRAME TGSBR76006
7 COVER TGSBR76007
8 PRESS PLATE BRACKET TGSBR76008
9 SPRING TGSBR76009
10 PRESSING PLATE TGSBR76010
11 MOVING CUTTER
PLATE
12.1 UPPER BRAKING DIE 10
INCH
12.2 UPPER BRAKING DIE 8
INCH
12.3 UPPER BRAKING DIE 6
INCH
12.4 UPPER BRAKING DIE 3
INCH
12.5 UPPER BRAKING DIE 2
INCH
12.6 UPPER BRAKING DIE 1
INCH
13 DIE CLAMPING PLATE TGSBR76013
14 HEX BOLT M10X60 TGSBR76014
15 ARM ROLLING WHEEL TGSBR76015
16 GUIDE TGSBR76016
17 ADJUSTABLE NUT TGSBR76017
18 HANDLE TGSBR76018
19 THREADED ROD TGSBR76019
20 POSITIONING ROD TGSBR76020
21 LIMITING BLOCK TGSBR76021
22 SUPPORTING PLATE TGSBR76022
23 BLADE TGSBR76023
24 BACK PRESSING ROLL TGSBR76024
25 LEAD SCREW TGSBR76025
26 NUT M10 TGSBR76026
27 ADJUSTABLE SCREW TGSBR76027
28 GREASE FITTING TGSBR76028
29 PRESS COVER TGSBR76029
TGSBR76011
TGSBR76012.1
TGSBR76012.2
TGSBR76012.3
TGSBR76012.4
TGSBR76012.5
TGSBR76012.6
30 GEAR TGSBR76030
31 LOWER ROLL TGSBR76031
32 UPPER ROLL TGSBR76032
33 PROTECTING COVER TGSBR76033
34 PIN (3X18) TGSBR76034
35 ECCENTRIC
MOUNTING
36 HANDLE
37 ROLLER ADJUSTMENT
KNOB
38 KEY TGSBR76038
39 SCREW M6X16 TGSBR76039
40 SCREW M6X12 TGSBR76040
41 BOLT M6X40 TGSBR76041
42 PIN 4X10
43 HANDLE TGSBR76043
44 SCREW M6X10 TGSBR76044
45 SCREW M10X45 TGSBR76045
46 WASHER TGSBR76046
47 HEX BOLT M12X60 TGSBR76047
48 HEX BOLT M10X25 TGSBR76048
49 WASHER TGSBR76049
50 HEX NUT M8-1.25 TGSBR76050
51 BOLT M12X40 TGSBR76051
52 SCREW M10X35 TGSBR76052
53 SCREW M8X25 TGSBR76053
54 SCREW M10X25 TGSBR76054
55 WASHER TGSBR76055
56 SCREW M8X80 TGSBR76056
57 SCREW M10X25 TGSBR76057
58 SCREW M6X12 TGSBR76058
59 SCREW M6X12 TGSBR76059
60 BUSHING TGSBR76060
61 NUT M10 TGSBR76073
TGSBR76035
32
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 33
SPECIFICATIONS
Part Number 6560030
Weight. 126 kg
Width/Depth/Height 905 x 390 x 565 mm
Capacities:
Maximum Workpiece Width 760 mm
Maximum Workpiece Thickness 1 mm
Pan/Box Brake Minimum Reverse Bend 9 mm
Pan/Box Brake Maximum Side Height @ 90° 105 mm
Slip Roll Minimum Cylinder Diameter 39 mm
Slip Roll Wire Sizes (L to R) 3.97 mm,4.37 mm, 5.56 mm
33
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 34
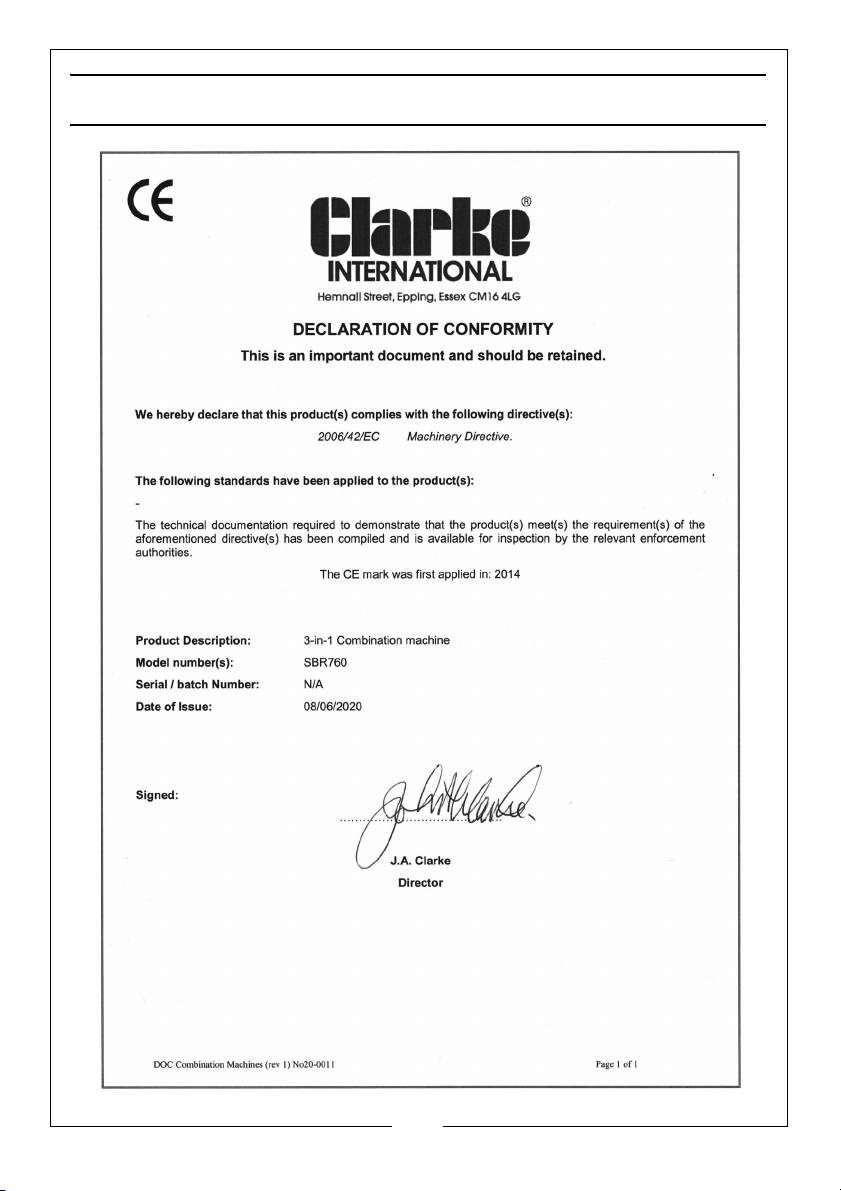
DECLARATION OF CONFORMITY
34
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 35
Page 36
 Loading...