

Page 1
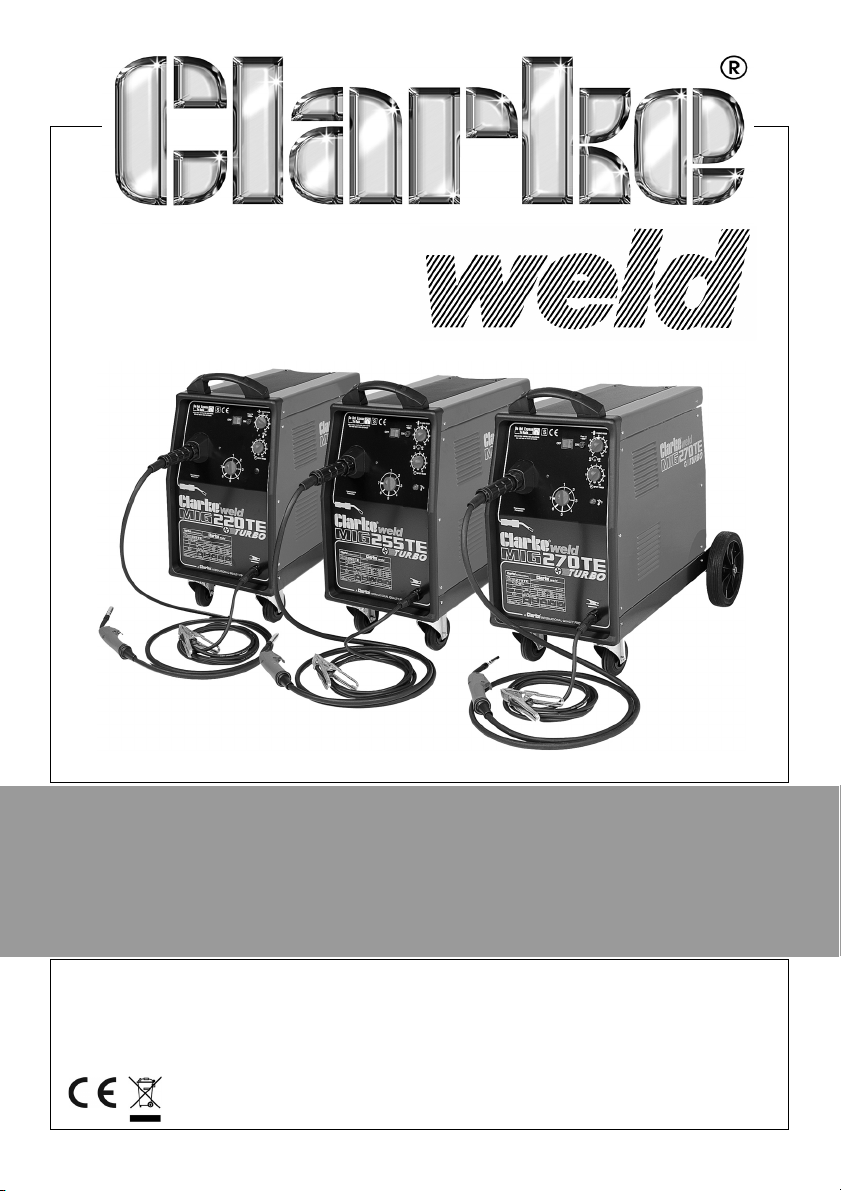
MIG WELDERS
MODEL NO: MIG220TE, MIG255TEC & MIG270TE
PART NO: 6015220, 6015510, 6015240
OPERATION & MAINTENANCE
INSTRUCTIONS
ORIGINAL INSTRUCTIONS 0218 ISS 7
Page 2
INTRODUCTION
Thank you for purchasing this CLARKE MIG Welder.
Before attempting to operate the machine, it is essential that you read this
manual thoroughly and carefully follow all instructions given. In doing so you
will ensure the safety of yourself and that of others around you, and you can
also look forward to the welder giving you long and satisfactory service.
GUARANTEE
This CLARKE product is guaranteed against faulty manufacture for a period of
12 months from the date of purchase. Please keep your receipt as proof of
purchase.
This guarantee is invalid if the product is found to have been abused or
tampered with in any way, or not used for the purpose for which it was
intended.
Faulty goods should be returned to their place of purchase, no product can
be returned to us without prior permission.
This guarantee does not effect your statutory rights.
ENVIRONMENTAL RECYCLING POLICY
Through purchase of this product, the customer is taking on the
obligation to deal with the WEEE in accordance with the WEEE
regulations in relation to the treatment, recycling & recovery and
environmentally sound disposal of the WEEE.
In effect, this means that this product must not be disposed of with
general household waste. It must be disposed of according to the laws
governing Waste Electrical and Electronic Equipment (WEEE) at a recognised
disposal facility.
Please note that the details and specifications contained herein, are correct
at the time of going to print. However, CLARKE International reserve the right
to change specifications at any time without prior notice. ALWAYS CONSULT
THE MACHINE’S DATA PLATE
2
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 3
GENERAL SAFETY PRECAUTIONS FOR ALL TYPES OF WELDING
WARNING: AS WITH ALL MACHINERY, THERE ARE CERTAIN HAZARDS
INVOLVED WITH THEIR OPERATION AND USE. EXERCISING RESPECT AND
CAUTION WILL CONSIDERABLY LESSEN THE RISK OF PERSONAL INJURY.
HOWEVER, IF NORMAL SAFETY PRECAUTIONS ARE OVERLOOKED, OR
IGNORED, PERSONAL INJURY TO THE OPERATOR MAY RESULT.
FAILURE TO FOLLOW THESE RULES MAY RESULT IN SERIOUS PERSONAL INJURY
GENERAL PRECAUTIONS
A) BURN PREVENTION
Wear protective clothing - gauntlet gloves designed for use in welding, apron,
and protective shoes. Button shirt collar and pocket flaps, and wear cuffless
trousers to avoid entry of sparks and slag. Wear helmet with safety goggles or
glasses with side shields underneath, appropriate filter lenses or plates
(protected by clear glass). This is a MUST for welding (and chipping) to protect
the eyes from radiant energy and spatter. Replace cover glass when broken,
pitted, or spattered. Avoid oily greasy clothing. A spark may ignite them. Hot
metal should never be handled without gloves. First aid facilities and a
qualified first aid person should be available unless medical facilities are close
by for immediate treatment of flash burns of the eyes and skin burns. Ear plugs
should be worn when working overhead or in a confined space. A hard hat
should be worn when others work overhead. Flammable hair preparations
should not be used by persons intending to weld or cut.
NOTE: ALL protective wear incl. masks & head shields MUST comply with
PPE Directive 89/686/EEC
B) TOXIC FUME PREVENTION
Severe discomfort, illness or death can result from fumes, vapours, heat, or
oxygen enrichment or depletion that welding (or cutting) may produce.
Prevent them with adequate ventilation. NEVER ventilate with oxygen. Lead-,
cadmium-, zinc-, mercury- and beryllium-, bearing materials, when welded (or
cut) may produce harmful concentrations of toxic fumes. Adequate local
exhaust ventilation must be used, or each person in the area as well as the
operator must wear an air- supplied respirator. For beryllium, both must be
used. Metals coated with or containing materials that emit toxic fumes should
not be heated unless coating is removed from the work surface, the area is
well ventilated, or the operator wears an air-supplied respirator. Work in a
confined space only while it is being force ventilated and, if necessary, while
wearing an air-supplied respirator. Vapours from chlorinated solvents can be
decomposed by the heat of the arc (or flame) to form PHOSGENE, a highly
toxic gas, and other lung and eye irritating products. The ultraviolet (radiant)
3
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 4
energy of the arc can also decompose trichloroethylene and
perchloroethylene vapours to form phosgene. DO NOT WELD or cut where
solvent vapours can be drawn into the welding or cutting atmosphere or
where the radiant energy can penetrate to atmospheres containing even
minute amounts of trichloroethylene or perchloroethylene.
C) FIRE AND EXPLOSION PREVENTION
Causes of fire and explosion are:
1. Combustibles reached by the arc, flame, flying sparks, hot slag or heated
material;
2. misuse of compressed gases and cylinders
3. short circuits.
BE AWARE that flying sparks or falling slag can pass through cracks, along
pipes, through windows or doors, and through wall or floor openings, out of
sight of the goggled operator.
To prevent fires and explosion: keep equipment clean and operable, free of
oil, grease, and (in electrical parts) of metallic particles that can cause short
circuits. If combustibles are in area, do NOT weld. Move the work if
practicable, to an area free of combustibles.
Avoid working in paint spray rooms, dip tanks, storage areas, ventilators. If the
work cannot be moved, move combustibles away from sparks and heat; or
protect against ignition with suitable fire- resistant covers or shields.
Walls, ceilings, and floor near work should be protected by heat resistant
covers or shields. Fire watcher must be standing by with suitable fire
extinguishing equipment during and for some time after welding or cutting if:
1. appreciable combustibles (including building construction) are within 10m.
2. appreciable combustibles are further than 10m, but can be ignited by
sparks.
3. openings (concealed or visible) in floors or walls can expose combustibles
to sparks.
4. combustibles adjacent to walls, ceilings, roofs or metal partitions can be
ignited by radiant or conducted heat.
After work, check that area is free of sparks, glowing embers, and flames. An
empty container that held combustibles, or that can produce flammable or
toxic vapours when heated, must never be welded on or cut, unless container
has first been cleaned. This includes a thorough steam or caustic cleaning (or
a solvent or water washing, depending on the combustible’s solubility)
followed by purging and inerting with nitrogen or carbon dioxide, and using
protective equipment.
Water filling just below working level may substitute for inerting.
4
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 5
A container with unknown contents should be cleaned (see paragraph
above), do NOT depend on sense of smell or sight to determine if it is safe to
weld or cut. Hollow castings or containers must be vented before welding or
cutting - they can explode.
In explosive atmospheres, never weld or cut where the air may contain
flammable dust, gas, or liquid vapours.
ELECTRIC ARC (MIG, TIG) WELDING
Comply with precautions in above, and this section. Arc welding, properly
done, is a safe process but a careless operator invites trouble. The equipment
carries high currents at significant voltages. The arc is very bright and hot.
Sparks fly, fumes rise, ultraviolet and infrared energy radiates and work pieces
are hot. The wise operator avoids unnecessary risks and protects himself and
others from accidents.
A) BURN PROTECTION
The welding arc is intense and visibly bright. It’s radiation can damage eyes,
penetrate lightweight clothing, reflect from light coloured surfaces and burn
the skin and eyes. Skin burns resemble acute sunburn, those from gas shielded arcs are more severe and painful.
DON’T GET BURNED! FOLLOW ALL SAFETY PRECAUTIONS!
PROTECTIVE CLOTHING
Wear long sleeved clothing (particularly for gas shielded arc) in addition to
gloves, apron and strong shoes. As necessary, use additional protective
clothing such as leather jacket or sleeves, flameproof apron, and fire-resistant
leggings. Avoid outer garments of untreated cotton. Bare skin protection:
Wear dark substantial clothing, Button collars closed to protect the chest and
neck and button any pockets to prevent entry of sparks.
EYE AND HEAD PROTECTION
Protect eyes from exposure to arc. NEVER look at an electric arc without
protection. Welding helmet or shield containing an appropriate filter plate
(Please refer to the section ‘Welding Shield). Place over face before striking
arc. Protect filter plate with a clear cover plate. Cracked or broken helmet or
shield should NOT be worn; radiation can pass through to cause burns.
Cracked, broken, or loose filter plates must be replaced IMMEDIATELY.Replace
clear cover plate when broken, pitted, or spattered. WE SUGGEST you wear
flash goggles with side shields under the helmet, to give some protection to
the eyes should the helmet not be lowered over the face before an arc is
struck. Looking at an arc momentarily with unprotected eyes (particularly high
5
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 6
intensity gas-shielded arc) can cause a retinal burn thatmay leave a
permanent dark area in the field of vision. Before welding whilst wearing
contact lenses, seek advice from your optician.
PROTECTION OF NEARBY PERSONNEL
For production welding, a separate, well vented room or enclosed bay is best.
In open areas,surround the operation with low reflective, non- combustible
screens or panels. Allow for free air circulation, particularly at floor level.
Provide face shields for all persons who will be looking directly at the weld.
Others working in the area should wear flash goggles. Before starting to weld,
make sure that screen or bay doors are closed.
B) TOXIC FUME PREVENTION
Comply with all precautions in 1B.
C) FIRE AND EXPLOSION PREVENTION
Do not overload arc welding equipment. It may overheat cables and cause a
fire. Loose cable connections may overheat or flash and cause a fire. Never
strike an arc on a cylinder or other pressure vessel. It creates a brittle area that
can cause a violent rupture or lead to such a rupture later under rough
handling.
D) SHOCK PREVENTION
Exposed live conductors or other bare metal in the welding circuit, or in
unearthed, electrically-LIVE equipment can fatally shock a person whose
body becomes a conductor. DO NOT STAND, SIT, LIE, LEAN ON, OR TOUCH a
wet surface when welding, without suitable protection.
PROTECTION FOR WEARERS OF ELECTRONIC LIFE SUPPORT DEVICES
(PACEMAKERS).
Magnetic fields from high currents can affect pacemaker operation. Persons
wearing pacemakers should consult with their doctor before going near arc
welding or spot welding operations.
E) PROTECTION AGAINST SHOCK:
Keep body and clothing dry. Never work in damp area without adequate
insulation against electric shock. Stay on a dry duckboard or rubber mat when
dampness or sweat can not be avoided. Sweat, sea water, or moisture
between body and an electrically LIVE part - or earthed metal - reduces the
body surface electrical resistance, enabling dangerous and possibly lethal
currents to flow through the body.
1) EARTHING THE EQUIPMENT
When arc welding equipment is earthed according to the National Electrical
Code, and the workpiece is earthed, a voltage may exist between the
electrode and any conducting object.
6
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 7
Examples of conducting objects include, but are not limited to, buildings,
electrical tools, work benches, welding power source cases, workpieces, etc.
Never touch the electrode and any metal object unless the welding power
source is off. When installing, connect the frames of each unit such as welding
power source, control, work table, and water circulator to the building earth.
Conductors must be adequate to carry earth currents safely. Equipment
made electrically LIVE by stray current may shock, possibly fatally. Do not
EARTH to electrical conduit, or to a pipe carrying ANY gas or a flammable
liquid such as oil or fuel.
2) TORCH
A fully insulated torch should be used without protruding screws or other
damage.
3) CONNECTORS
Fully insulated lock-type connectors should be used to join welding cable.
4) CABLES
Frequently inspect cables for wear, cracks and damage. IMMEDIATELY
REPLACE those with excessively worn or damaged insulation to avoid possibly
lethal shock from bared cable. Cables with damaged areas may be taped to
give resistance equivalent to original cable. Keep cable dry, free of oil and
grease and protected from hot metal and sparks.
5) TERMINALS AND OTHER EXPOSED PARTS
Terminals and other exposed parts of electrical units should have insulating
covers secured before operation.
6) SAFETY DEVICES
Safety devices such as interlocks and circuit breakers should not be
disconnected or shunted out. Before installation, inspection, or service of
equipment, shut OFF all power and remove line fuses (or lock or red-tag
switches) to prevent accidental turning ON of power. Do not open power
circuit or change polarity while welding. If, in an emergency, it must be
disconnected, guard against shock burns, or flash from switch arcing. Always
shut OFF and disconnect all power to equipment. A power disconnect switch
must be available near the welding power source.
7
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 8
PREPARATION OF THE WORKING AREA
The working area must be sufficiently spacious, not humid, and well-ventilated
as to avoid any fumes which develop from the welding process and from
incidental material adhering to the pieces to be welded (oils, paints, tars...)
which may cause danger to the operator.
Avoid welding tanks which may contain flammable residuals.
WARNING: ELECTRIC SHOCK CAN BE FATAL. A PERSON QUALIFIED IN FIRST
AID SHOULD ALWAYS BE PRESENT IN THE WORKING AREA. IF PERSON IS
UNCONSCIOUS AND ELECTRIC SHOCK IS SUSPECTED, DO NOT TOUCH
THE PERSON IF HE OR SHE IS IN CONTACT WITH THE WELDER OR CABLES.
DISCONNECT THE WELDER FROM THE POWER SOURCE AND THEN USE FIRST
AID. DRY WOOD, OR OTHER INSULATING MATERIAL CAN BE USED TO
MOVE CABLES, IF NECESSARY, AWAY FROM THE PERSON.
ADDITIONAL SAFETY PRECAUTIONS FOR MIG WELDING
1. ALWAYS ensure that there is full free air circulating around the outer casing
of the machine, and that the louvres are unobstructed.
2. Welding arc can seriously damage your eyes. Both operator and
spectators must ALWAYS use a proper welding face shield or helmet with
suitable filter lenses. Proper gloves and working clothes should be worn at
all times.
3. ALWAYS check that the pressure regulator and gauges (where fitted), are
working correctly. DO NOT lubricate the regulator.
4. ALWAYS use the correct regulator. Regulators are designed to be used with
a specific gases.
5. ALWAYS inspect the torch hose before use to ensure it is in good condition.
6. ALWAYS keep the free length of torch hose outside the work area.
7. ALWAYS remove all flammable materials from the welding area.
8. NEVER remove any of the panels unless the machine is disconnected from
the supply, AND never use the machine with any of the panels removed.
8
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 9
9. The MIG welding process uses an INERT gas to protect the weld pool. It
isimportant to ensure the appropriate gas is being used. NEVER use gas
from a cylinder, the content of which is unknown.
NEVER
a. Use a damaged cylinder.
b. Lift the cylinder by the valve.
c. Expose the cylinder to a heat source or sparks.
10. NEVER use or store in a damp environment. DO NOT EXPOSE TO RAIN.
11. ALWAYS keep fire extinguisher handy....’Dry Powder, C02 or BCF, NOT Water
12. NEVER attempt any electrical or mechanical repair unless your are a
qualified technician. If you have a problem with the machine contact your
local CLARKE dealer.
13. NEVER continue to weld, if, at any time, you feel even the smallest electric
shock. Stop welding IMMEDIATELY and DO NOT attempt to use the
machine until the fault is diagnosed and corrected.
14. NEVER point the MIG torch at any person or animal.
15. NEVER touch the MIG torch nozzle until the welder is switched OFF and the
nozzle has been allowed to cool.
16. NEVER connect, disconnect, or attempt to service the welding torch, until
the machine is switched OFF and disconnected from the mains supply.
17. NEVER allow the earth cable or torch hose to become wrapped around
the operator or any person in the vicinity.
A comprehensive range of CLARKE safety equipment for use when welding is
available from your local dealer.
9
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 10
ELECTROMAGNETIC INTERFERENCE (EMC)
Whilst this unit complies with EMC regulations, the user is responsible for
installing and using the welding equipment correctly. If electromagnetic
disturbance is detected it is the responsibility of the user to resolve the
situation. Remedial action may be as simple as earthing the welding circuit,
see ‘Note’. In other cases it could involve constructing an electromagnetic
screen enclosing the power source and the work complete with associated
input filters.
NOTE: The welding circuit may or may not be earthed for safety reasons.
Changing the earthing arrangements should only be authorised
by a person who is competent to assess whether the changes will
increase the risk of injury, e.g. by allowing parallel welding current
return paths which may damage the earth circuits of other
equipment.
ASSESSMENT OF AREA
Before installing welding equipment the user shall make an assessment of
potential
electromagnetic problems in the surrounding area. Avoid using your welder in
the vicinity of:
1. other supply cables, control cables, signalling and telephone cables;
above, below and adjacent to the welding equipment;
2. radio and television transmitters and receivers;
3. computer and other control equipment;
4. safety critical equipment, e.g. guarding of industrial equipment;
5. pacemakers and hearing aids etc;
6. equipment used for calibration or measurement;
7. other equipment in the environment. The user shall ensure that other
equipment being used in the environment is compatible. This may require
additional protection measures.
It may be possible to avoid the above by choosing the time of day that
welding or other activities are to be carried out.
The size of the surrounding area to be considered will depend on the structure
of the building and other activities taking place. The surrounding area may
extend beyond the boundaries of thepremises.
METHODS OF REDUCING EMISSIONS
Welding equipment will be connected to the mains supply but if interference
occurs, it may be necessary to take additional precautions such as filtering of
10
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 11
the mains supply. Consideration should be given to shielding the supply cable
of permanently installed welding equipment, in metallic conduit or equivalent.
Shielding should be electrically continuous throughout its length.
The shielding should be connected to the welding power source so that good
electrical contact is maintained between the conduit and the welding power
source enclosure.
The welding equipment should be routinely maintained according to the
manufacturer’s recommendations. All access and service doors and covers
should be closed and properly fastened when the welding equipment is in
operation. The welding equipment should not be modified in any way except
for those changes and adjustments covered in the manufacturer’s
instructions. In particular, the spark gaps of arc striking and stabilizing devices
should be adjusted and maintained according to the manufacturers
recommendations.
The welding cables should be kept as short as possible and should be
positioned close together, running at or close to the floor level.
Bonding of all metallic components in the welding installation and adjacent to
it should be considered. However, metallic components bonded to the work
piece will increase the risk that the operator could receive a shock by
touching these metallic components and the electrodes at the same time.
The operator should be insulated from all such bonded metallic components.
Where the workpiece is not bonded to earth for electrical safety, nor
connected to earth because of its size and position, e.g. ships hull or building
steelwork, a connection bonding the workpiece to earth may reduce
emissions in some, but not all instances.
Care should be taken to prevent the earthing of the workpiece increasing the
risk of injury to users, or damage to other electrical equipment.
Where necessary, the connection of the workpiece to earth should be made
by a direct connection to the workpiece, but in some countries where direct
connection is not permitted, the bonding should be achieved by suitable
capacitance, selected according to national regulations.
Selective screening and shielding of other cables and equipment in the
surrounding area may alleviate problems of interference. Screening of the
entire welding installation may be considered for special applications.
11
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 12
ELECTRICAL CONNECTIONS
WARNING: THIS APPLIANCE MUST BE EARTHED.
MIG 220TE & 255TEC
Connect the mains lead, through a suitably fused isolator switch, to a 230 Volt
(50Hz) electrical supply, having a fuse rating in accordance with that given in
the specification chart on page 2. A standard 13 Amp plug MUST NOT be used
with this machine.
IMPORTANT: The wires in the mains lead are coloured in accordance with the
following code: Green & Yellow - Earth, Blue - Neutral, Brown - Live
As the colours of the flexible lead of this appliance may not correspond with
the coloured markings identifying terminals in your electrical supply, proceed
as follows:
• Connect the GREEN & YELLOW coloured cord to terminal marked with a
letter “E” or Earth symbol “ ”
• Connect BROWN cord to terminal marked with a letter “L”
• Connect BLUE cord to terminal marked with a letter “N”.
MIG 270TE
This model is designed for use with a 400V three-phase supply, and should be
connected through a suitably fused isolator switch.
The GREEN or GREEN & YELLOW wire should be connected to the EARTH
terminal or terminal marked with “ ” symbol. The other two wires are for
connection to the phase wires.
CABLE EXTENSIONS:
IMPORTANT: For extensions up to 10m, the size of the conductors MUST be at
least the same size as that used on the machine - 2.5mm2. It is NOT advised
to use extensions greater than this, but if it is absolutely necessary, the
conductor size must be 4mm2 up to a maximum of 25m in length.
WARNING: NEVER OPERATE THIS MACHINE WITH THE SIDE PANELS
PARTIALLY OPENED OR COMPLETELY REMOVED
12
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 13
MIG WELDING - PRINCIPLES OF OPERATION
MIG (Metal Inert Gas) welding is a process in which a power wire electrode is
fed continuously into the weld pool at a controlled, constant rate. The wire is
connected to the positive side of a rectified voltage supply. The workpiece is
connected to the negative side of the supply. When the wire is fed, it comes into
contact with the workpiece and an arc is struck. The arc melts the wire and the
material, fusing it together. The wire, which is fed by the wire feed motor is fed
into the weld pool, burning itself off at a rate dependent upon the selected wire
feed speed. To protect the weld pool from oxidation and impurities during the
welding process, a shielding gas flows over and around the weld pool. This gas
flow must be sufficient to protect the weld, but not be wasteful.
NOTE: Poor gas coverage will result in poor welding. Excessive gas
coverage is wasteful and expensive.
BENEFITS OF MIG WELDING
• 50% faster welding time.
• Operator training time kept to a minimum.
• There is no slag removal, thus eliminating almost all post-welding cleaning
operations.
• Minimum waste of welding consumables.
• Overall, a faster more efficient way of getting the job done.
• Less heat - less distortion.
• Ability to weld thin material.
13
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 14
UNPACKING & PARTS IDENTIFICATION
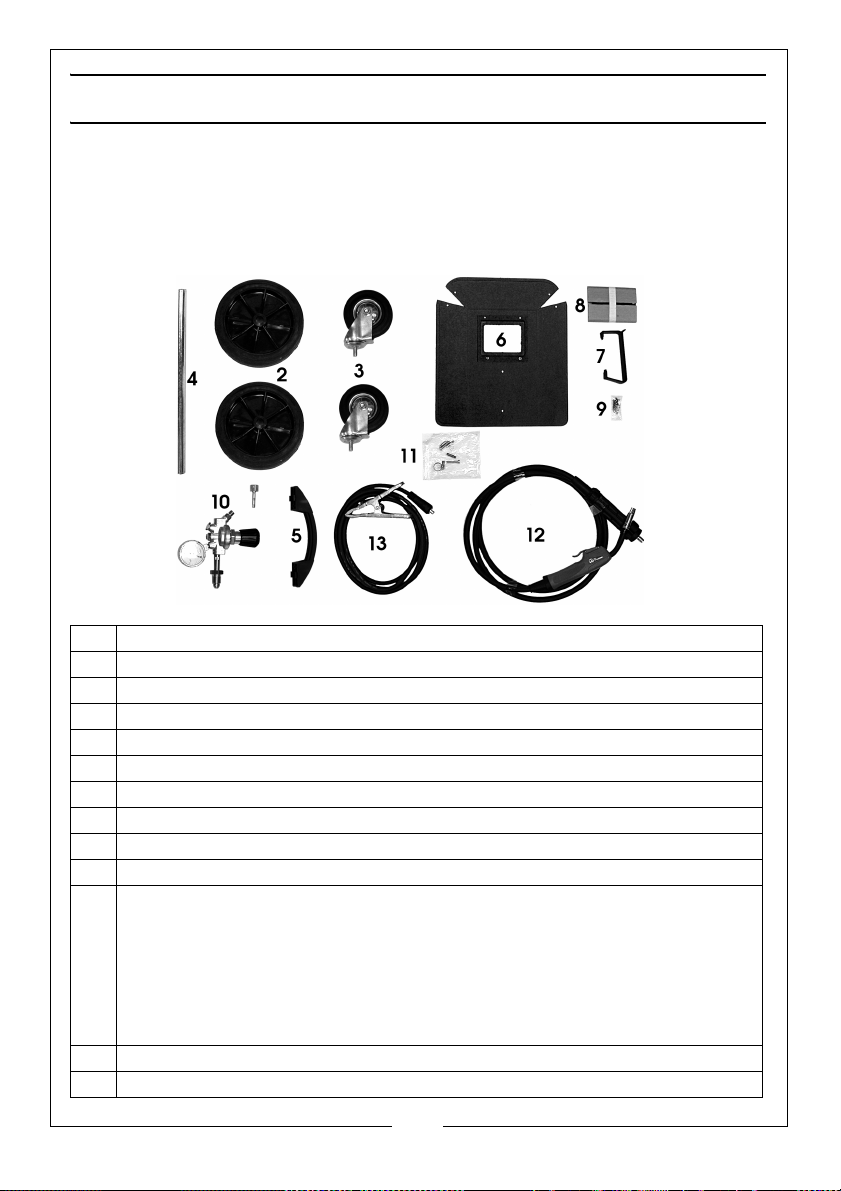
Unpack and lay out the components, checking against the following list. Any
damage or deficiency should be reported to your CLARKE dealer
immediately.
Some components are stored within the side compartment. To open the
compartment, slide the recessed handle backwards.
1 Welder complete with power cable and gas hose.
2 2 x Wheels
3 2 x Castors
4 1 x Tubular Axle
5 1 x Handle
6 1 x Welding Mask
7 1 x Welding Mask Handle
8 1 x Package containing 1x Clear Glass and 1x Dark Glass Lens
9 1 x Package containing 6 screws and nuts for welding mask
10 1 x Gas Regulator with nut and tail connector.
11 1 x Package containing:
• 2 x circlips for wheel axle (wheel retainers)
• 2 x Hex. socket head screws for securing the handle.
• Worm drive hose clip for gas hose to regulator
• 3 x spare welding tips...0.6mm and 0.8mm
A 0.6mm tip is also fitted to the torch
12 Torch & Hose Assembly
13 Earth Lead Assembly
14
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 15
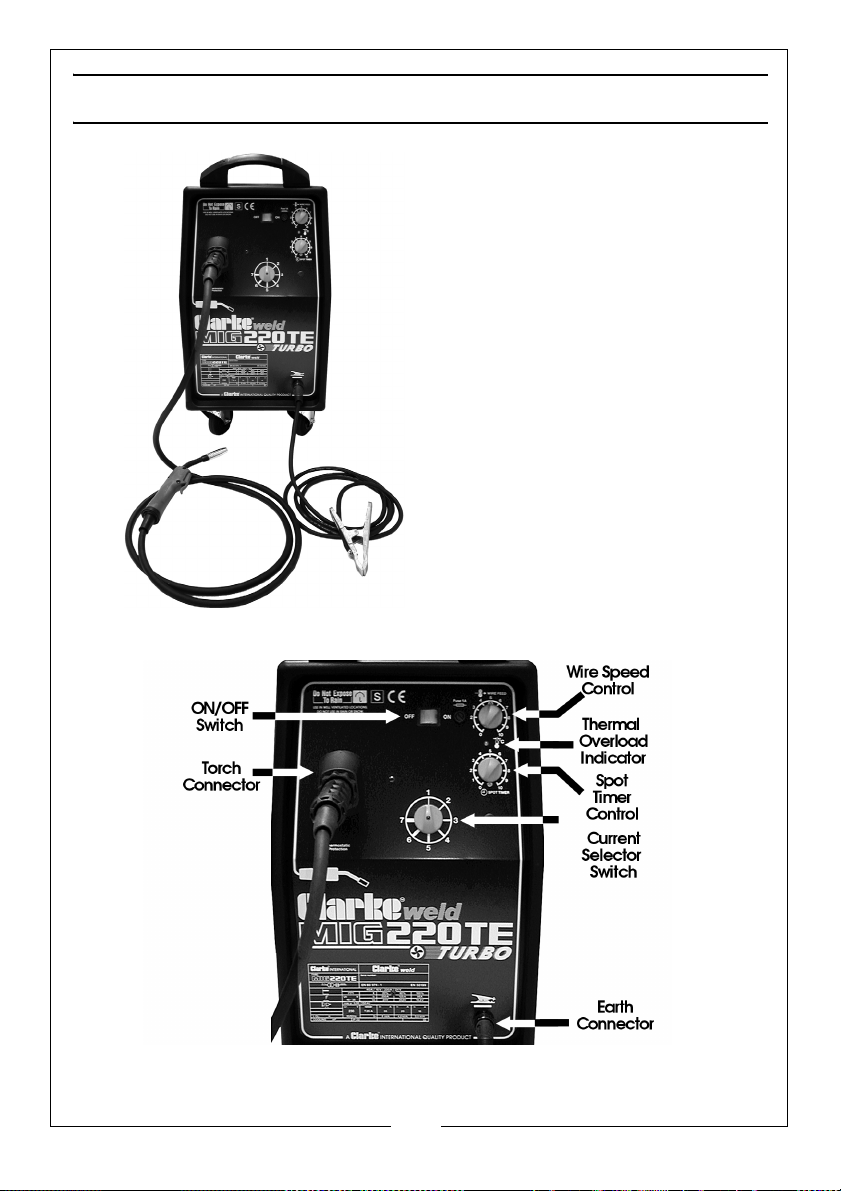
GENERAL LAYOUT
FIG.2
15
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 16
ASSEMBLY
WHEELS & CASTORS
Raise the machine and thread the axle into its housing and attach the wheels,
securing with the circlips provided.
Thread the castors into their mountings and tighten the bolts.
HANDLE
Attach the handle to the top front of the machine using the two hex. socket
head screws.
HOSE AND EARTH CABLE
Simply screw the Torch Hose connector into the adapter on the front panel,
ensuring the pins are correctly aligned. DO NOT force it into place.
Tighten the large plastic round nut.
The earth cable plug is inserted into its receptacle on the lower front panel,
ensuring the key lines up with the keyway, and then rotated through 90
degrees to lock into place.
GAS SUPPLY
It is necessary to obtain a cylinder of gas suitable for the job in hand.
Locate the gas cylinder on the platform at the rear of the unit and secure
using the chain provided.
A regulator is provided, complete with outlet pressure gauge for use with
argon or argon mix gas bottles. Should you wish to use Carbon Dioxide, it will
be necessary to purchase an appropriate regulator with a female connector.
Your Clarke dealer will be happy to advise in this regard.
Ensure the outlet of the gas bottle is clean, then screw on the regulator and
nip up... do not overtighten.
Always use the appropriate gas for the material being welded. If you are
unsure, consult a qualified tradesman or a suitable reference book.
Attach the nut and tail to the gas hose using the worm drive clip provided,
then screw the nut on to the regulator outlet and tighten.
Open the gas valve and screw in the regulator knob allow gas into the system
to check for gas leaks. If any are found they must be rectified before
proceeding. Turn off the gas when satisfied the system is leak free.
16
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 17
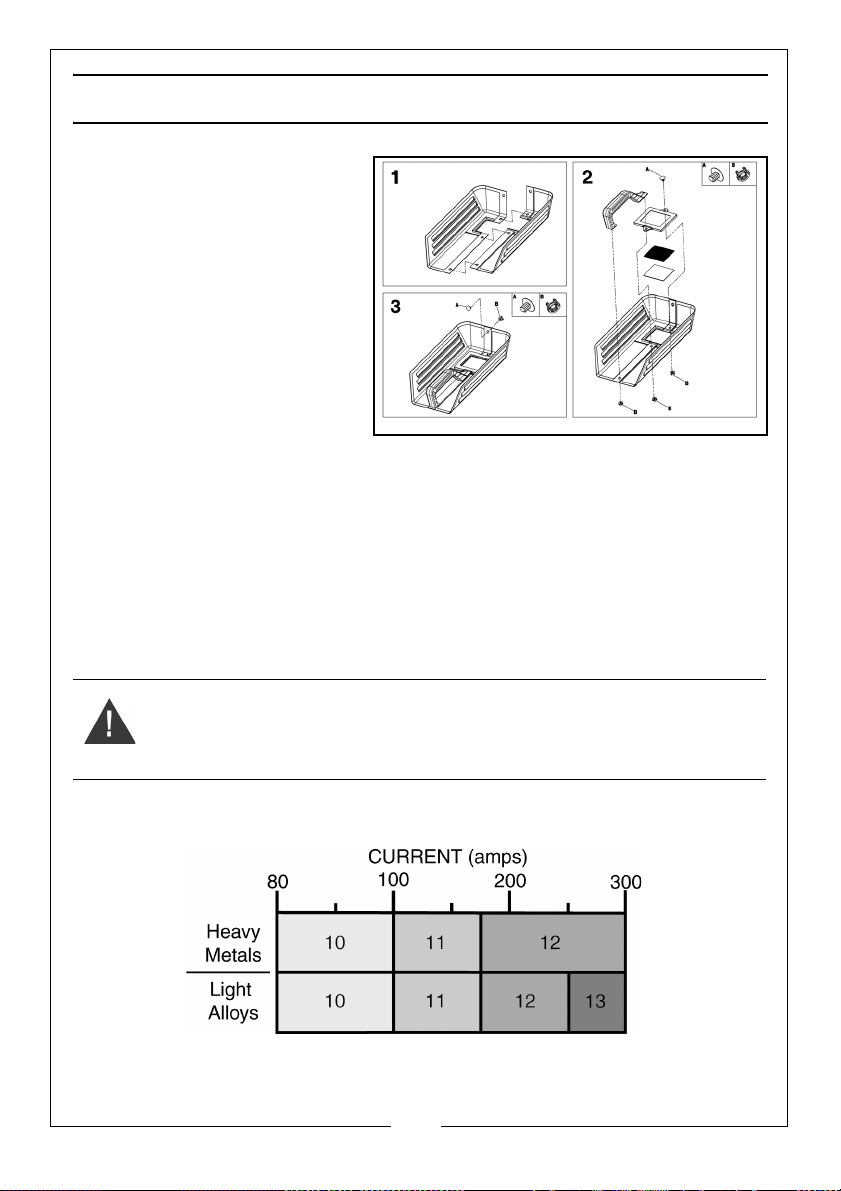
THE WELDING SHIELD
1. Push the two halves of the
shield together as shown.
2. Place the handle into
position and secure using
the plastic screw and clip
provided
3. Working from the inside of
the shield, insert the clear
glass panel into the recess
in the shield, followed by
the dark glass panel.
4. Secure the glass panels with
the lens surround and plastic screws/clips provided. The clear glass MUST
be on the outside of the shield.
5. Finally use the last plastic screw and clip as shown to fix the two halves of
the shield together.
It is important to pay attention to the notes on welding shield maintenance.
When replacing the glass panels, ONLY use those parts supplied by Clarke
International. The dark panel is a certified, specific optical class, and should
not be exchanged for any other type. The clear glass panel should be
replaced when it becomes badly pitted.
WARNING: NEVER LOOK AT AN ELECTRIC ARC WITHOUT EYE PROTECTION
AS THIS CAN INJURE THE EYES PERMANENTLY. ALWAYS USE A
PROTECTION MASK OR WELDING HELM
NOTE: The correct shade of glass should be used in accordance with the
following chart:
All components are now correctly assembled, and the welder may now be
prepared for use as follows.
17
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 18
PREPARATION FOR USE
INSTALLING THE WELDING WIRE
NOTE: These machines are designed to accept either the Clarke 5kg or
15kg wire spools of mild steel, stainless steel or aluminium
according to the type of metal you wish to weld. Wire spools must
be purchased separately. See your Clarke dealer for full details.
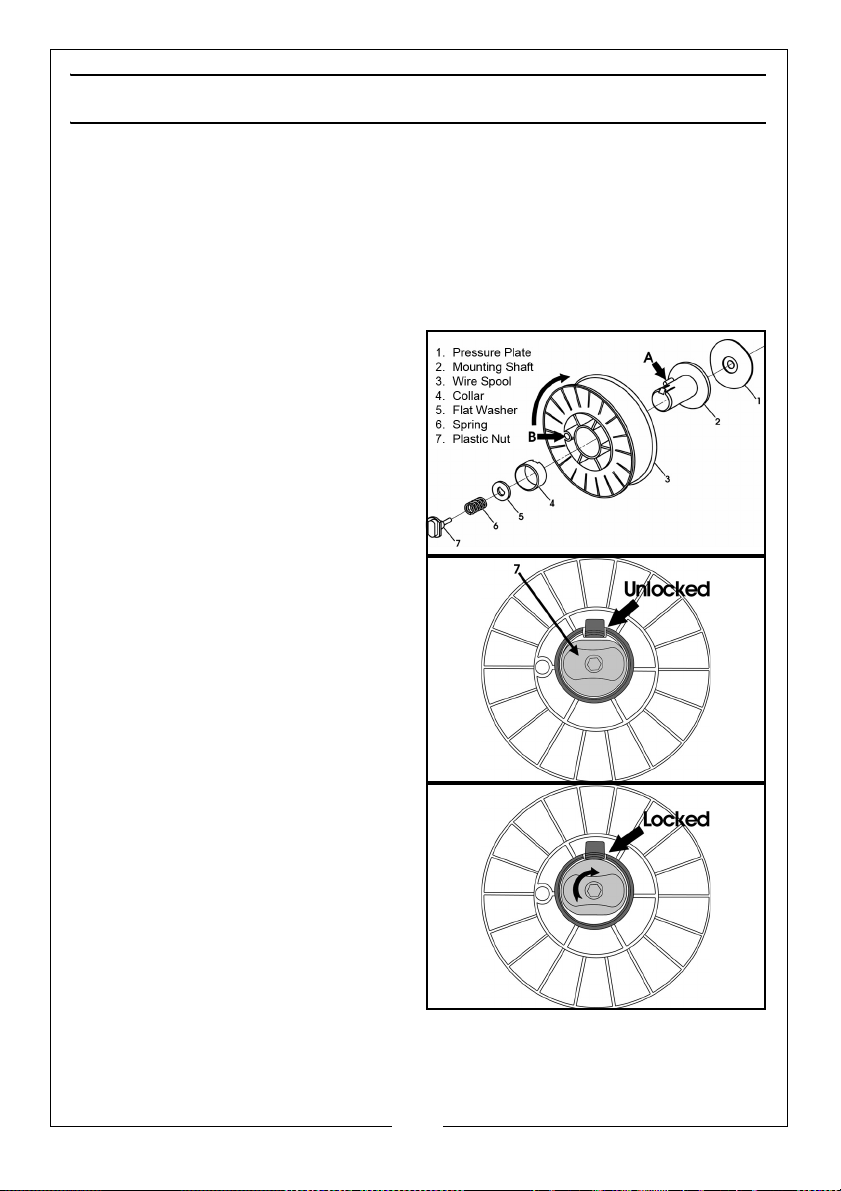
1. IMPORTANT: Ensure that the gas and electrical supplies are disconnected.
2. To fit the wire spool shown in Fig 4,
firstly open the side compartment
by pulling the recessed catch
backwards.
3. Turn the plastic knob with cam (7)
to the position shown in Fig 5, so
that the latch is unlocked, and
pull off the collar (6).
4. Slide the spool on to the shaft,
ensuring that the Peg ‘A’ locates
snugly in locating hole ‘B’,
ensuring the direction of feed of
the wire is in the direction of the
arrow.
5. Replace the collar - 4, (5kg spool
ONLY), and turn the plastic knob
with the cam (7) to the position
shown in Fig 6, thereby locking the
spool on the shaft.
NOTE: The plastic knob, (item 7 - Fig
4), is also used to apply slight
tension to the wire spool. This
prevents the spool from
running freely, which could
cause the wire to unspool,
creating a ‘birds nest’ tangle within the side compartment. Adjust
by hand and test the tension.
18
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 19
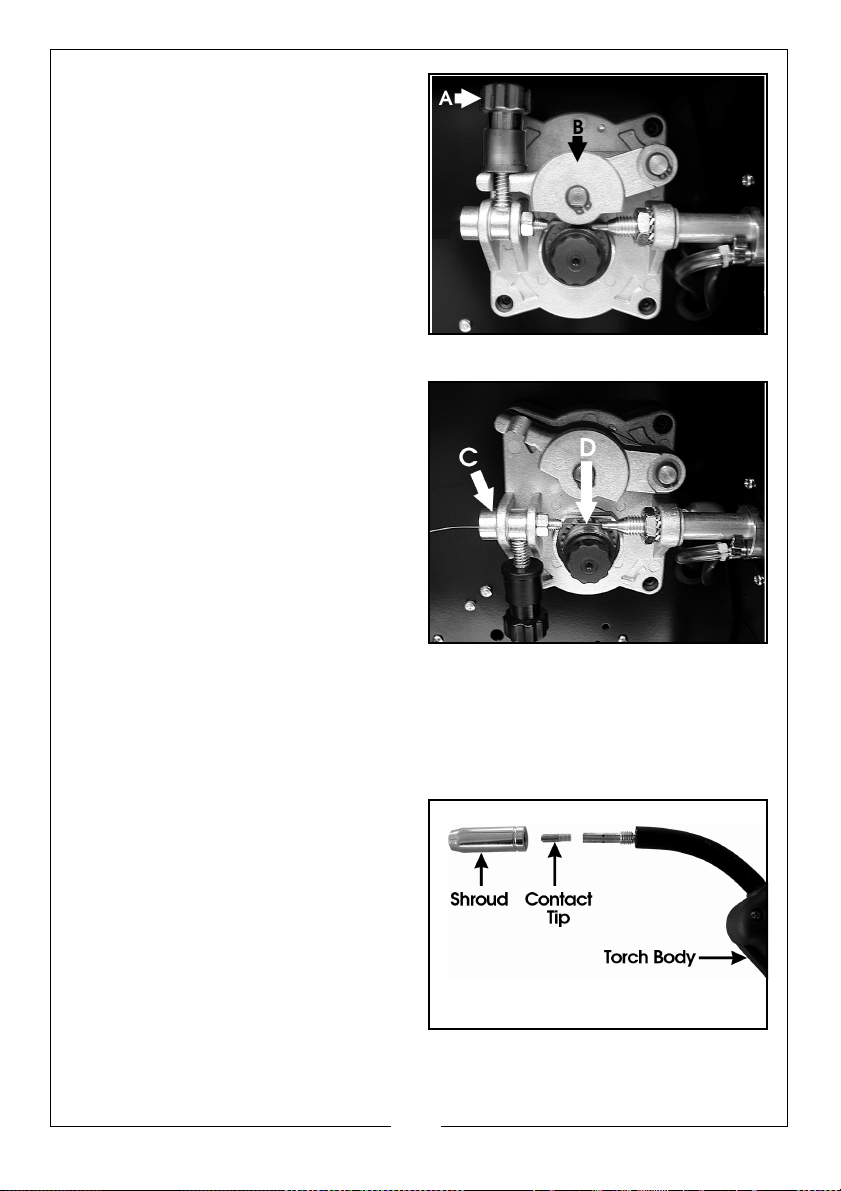
6. Unscrew the pressure roller
bracket securing knob (A, in Fig
7), whilst holding down the
pressure roller bracket (B), against
spring pressure, so that the screw
rod hinges out of its slot. This
releases the pressure roller
bracket which, when released,
will pivot upwards under spring
pressure.
IMPORTANT: Before fitting any wire,
ensure the correct groove on the
roller is in place. (See page 19).
7. Pull out the end of the wire from
the rim of the spool, taking care
NOT to release it. The spool is
wound firmly and should remain
this way.
Ensuring the wire is straight and
not kinked in any way, clip off the
end with a sharp pair of snips
ensuring there are no burrs or
sharp edges.
Proceed to feed it through the
guide tube (C, Fig 8), over the
groove on the roller (D), and into
the wire liner, by about 10 - 15 cm.
8. Reposition the pressure roller bracket and securing knob (A) and tighten
slightly.
Tightening the knob (A) too tightly will crush the wire and damage the wire
feed motor, too loose will not allow the wire to be pulled by the roller.
9. (Ref. Fig 9) Remove the torch
shroud by twisting it anti clockwise
and pulling it off, then unscrew
the contact tip. Should any wire
protrude from the tip....pull it out
completely and discard.
10. Close the side panel of the
machine and switch on at the
mains or isolator.
19
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 20
11. Set the wire feed rotary switch on the front panel to position 6 or 7, switch
on the machine and press the trigger.
The wire will feed through the hose and when it appears at the torch end,
release the trigger, switch off the machine and disconnect from the mains
supply. Replace the contact tip and the torch shroud.
IMPORTANT: Ensure the hose is kept straight during this operation, to assist
the wire as it is fed through to the wire liner and torch.
SELECTING THE CORRECT DRIVE ROLLER GROOVE
As previously mentioned, it is important that the correct groove in the drive
roller is selected for the particular wire being used. The roller provided has 0.6
and 0.88mm grooves.
The welder is factory set with the 0.8mm groove in position.
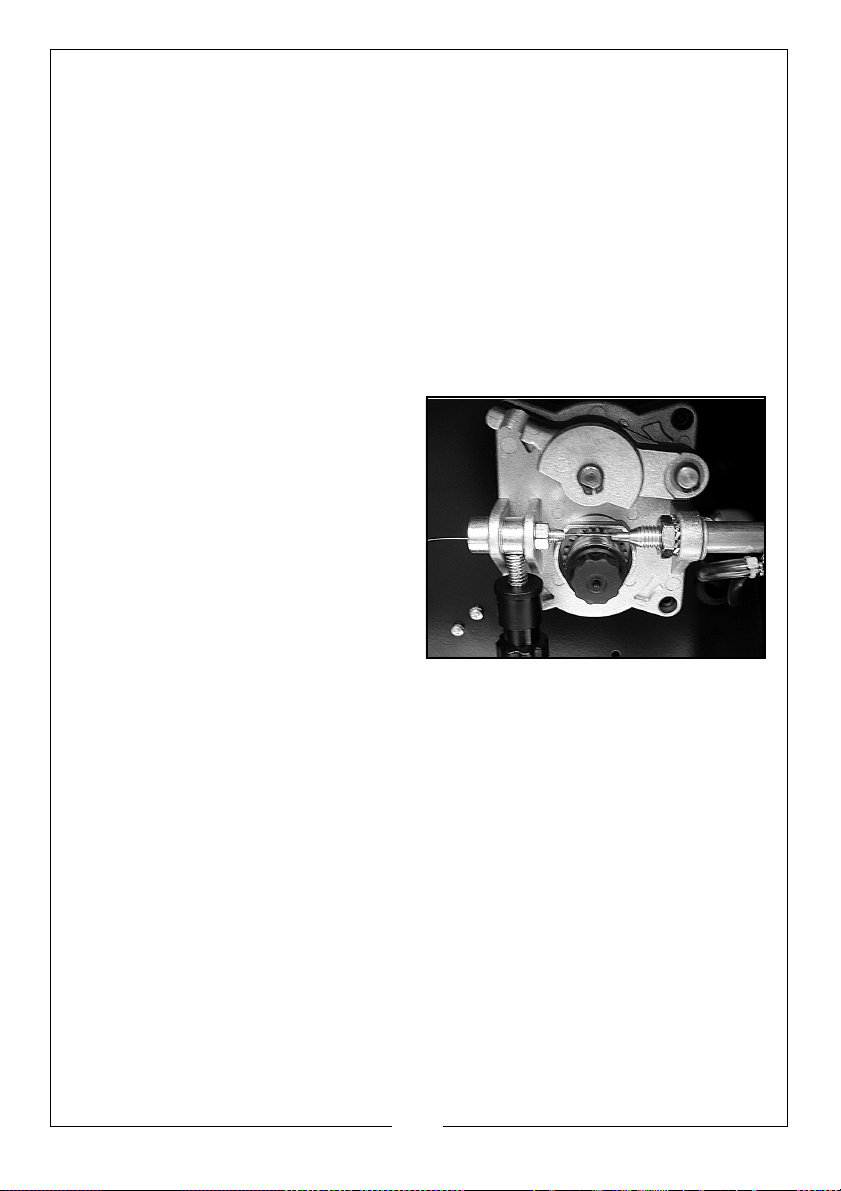
To change grooves, proceed as
follows:
1. With the pressure roller bracket
raised, and the old wire removed,
remove the roller securing knob
(arrowed), by turning it fully anticlockwise, then pull the roller from
the shaft.
2. Ensure the appropriate groove is
facing inwards before sliding the
roller on to the shaft.
Screw on the securing knob to
lock the roller securely in place.
20
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 21
OPERATION
Each time you use the machine it will be necessary to perform the following
operations:
CHECK THE WELDING WIRE
Check to ensure the correct type of welding wire is installed for the job in hand
and is correctly adjusted.
PREPARE THE WORK
MOST IMPORTANT! It is vital that the workpiece is perfectly clean at the point of
weld. Any coating, plating or corrosion MUST be removed, otherwise a good
weld will be impossible to achieve.
SET THE CONTROLS
In order to produce a satisfactory weld, the controls must be fine tuned
whenever there is a material change in weld characteristics. This is generally
referred to as ‘Tuning the Welder’.
The tuning of a MIG welding machine requires some practice, due to the fact
that - contrary to the arc welding procedure - two parameters must be
accommodated to achieve a perfect weld.
These are:
(1) Welding Current, and (2) Wire Feed Speed,
It is important to arrive at the correct combination to suit the type and
thickness of material to be welded.
The current, necessary for welding, is directly related to the wire feed speed.
As the current is increased, the wire feed speed is also increased.
Conversely, if current is decreased the wire feed speed is decreased.
A change in wire diameter results in changed parameters. A smaller diameter
wire requires an increase in wire feed speed to reach the same current.
If certain limits are exceeded, a satisfactory weld cannot be obtained. These
are:
A) An excessive wire feed speed (too high with regard to the welding current),
results in pulsing within the torch. This is because the wire electrode dips into
the puddle and cannot be melted off fast enough.
B) If the welding current is set too high, large drops can be seen at the end of
the wire electrode. These drops are often deposited beside the welding seam.
The correct rate of wire feed speed and welding current, results in very little
spatter and a continuous, intensive hissing can be heard from the arc.
21
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 22
(I) WELDING CURRENT CONTROL
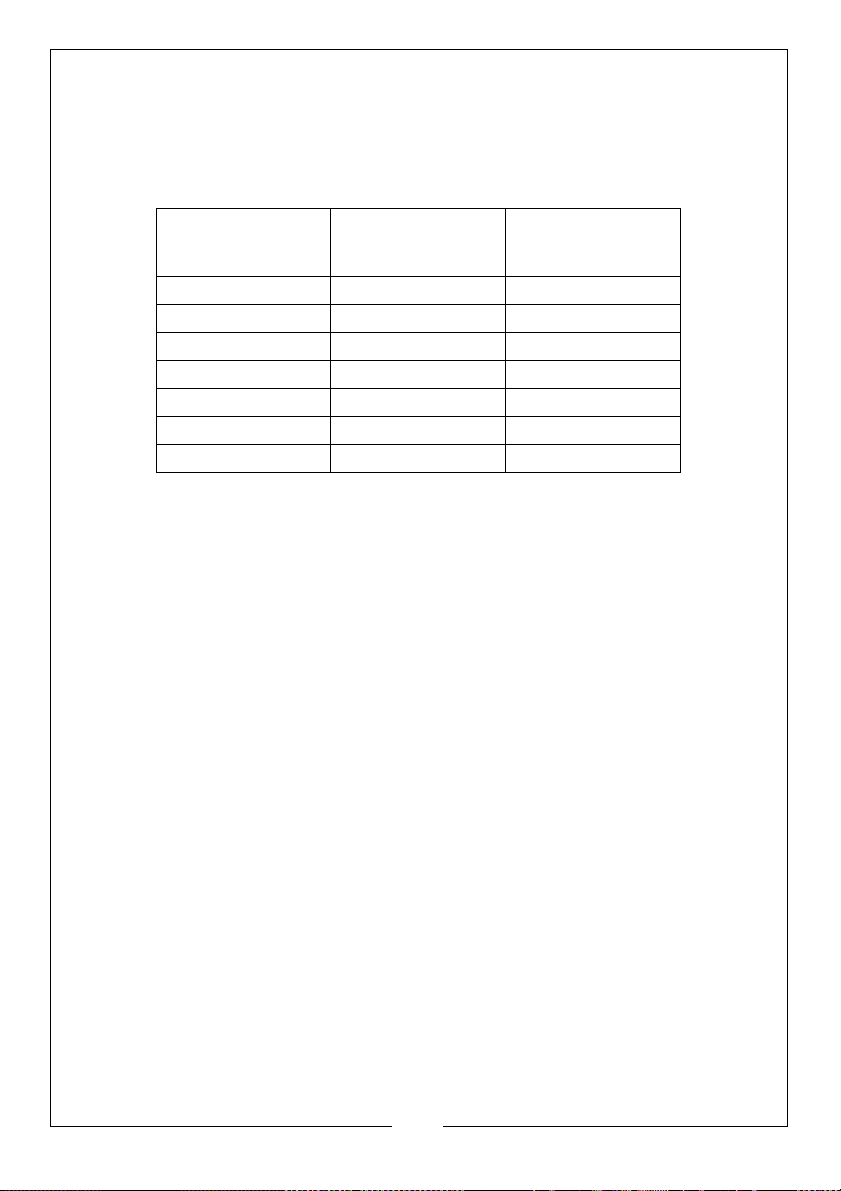
Select the welding current according to the type of metal and thickness to be
welded. The control has 7 positions as indicated in the chart below.
Experience will determine the optimum setting for the job in hand, but the
chart gives general settings from which to work.
Switch
Positions
10.6LOW
20.6LOW
3 0.6 - 0.8 MEDIUM
4 0.6 - 0.8 MEDIUM
5 0.8 MEDIUM - HIGH
6 0.8 HIGH
7 1.0 HIGH
Steel Wire
Diameter
(mm)
Wire Speed
Adjustment
NOTE: If the current and hence the wire speed is increased, the volume
of gas at the nozzle must also be increased. Turn the regulator
knob accordingly.
(II) WIRE FEED SPEED CONTROL
The WIRE FEED Rotary Control Knob, with graduations from 0 to 10, is used to
fine tune the wire speed feed to the nozzle. The knob should be set to position
6 to begin with for welding steel, and 8 for welding aluminium, then adjusted
as required.
NOTE: This control is for fine tuning the wire speed. The speed of wire
delivery will increase automatically as the current is increased
and vice versa. Therefore, once the ideal speed is achieved by
fine tuning, it should not be necessary to adjust this control when
the welding current is changed. It is always better to start with too
high a speed, and back off slightly, to avoid the possibility of the
wire welding itself to the tip.
TIMER CONTROL
This is explained in more detail on page 23. For all normal welding operations,
set this control to zero.
WELDING WIRE
Trim the welding wire so that it protrudes no more than 5mm from the end of
the shroud.
22
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 23
THE EARTH CLAMP
Attach the earth clamp to the workpiece as close to the point of weld as
possible, without it being intrusive. Ensure there is good contact and if
necessary, clean the area with a wire brush beforehand.... Remember, the
contact MUST be on bare metal - thoroughly clean.
THE GAS VALVE
Open the gas valve on the gas cylinder. Regulate the pressure by turning the
regulator knob clockwise (to increase pressure), and adjust to the desired
setting. NOTE: this varies with different metals, thicknesses and currents. Refer
to a MIG welding manual for instructions.
Your welder is now fully prepared for welding as follows:
With the welding current set, and welding wire trimmed, set the wire feed
control to 6, (8 for aluminium).
Plug the machine into the mains supply or switch on at the isolator and
ensuring all precautions have been taken and with the machine set up
correctly, switch ON the machine and lower the torch to the workpiece with
one hand, whilst holding the welding mask in the other.
Approach the work with the tip at an angle of approx. 45O and pull the torch
trigger fully. A welding current is now available at the tip and gas will be
issued.
As the wire touches the workpiece, an arc will be struck......BEFORE it is struck,
cover the face with the face mask.
Maintain a gap of approx. 5 - 7mm from the workpiece to the tip, and feed
the wire into the molten pool at a steady rate, along the line of the proposed
weld.
The speed of weld will depend upon the wire speed and welding current.
NOTE: As MIG welding is an acquired skill, it is strongly advised that, if you
are not fully familiar with this type of welding, you practice on a
piece of material with the same characteristics as your
workpiece, until you are satisfied with the result, and you have
fine tuned your welder to produce a satisfactory weld.
NOTE: One of the problems experienced with novice welders, is the
welding wire sticking to the contact tip. This is as a result of the
wire feed speed being too slow. It is always better therefore to
start with too high a speed, and back off slightly, to avoid the
possibility of the wire welding itself to the tip. This is the reason
position 6 is recommended for start up.
NOTE: The Wire Feed control is for fine tuning the wire speed. The speed
of wire delivery will increase automatically as the current is
increased from MIN to MAX, and vice versa. Therefore, once the
23
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 24
ideal speed is achieved, by fine tuning, it should not be necessary
to adjust this control when the welding current is changed.
NOTE: Listen to the sound made. An irregular crackling sound denotes
too high a wire speed. Decrease the speed until a regular, strong
buzzing sound is heard.
GENERAL INFORMATION
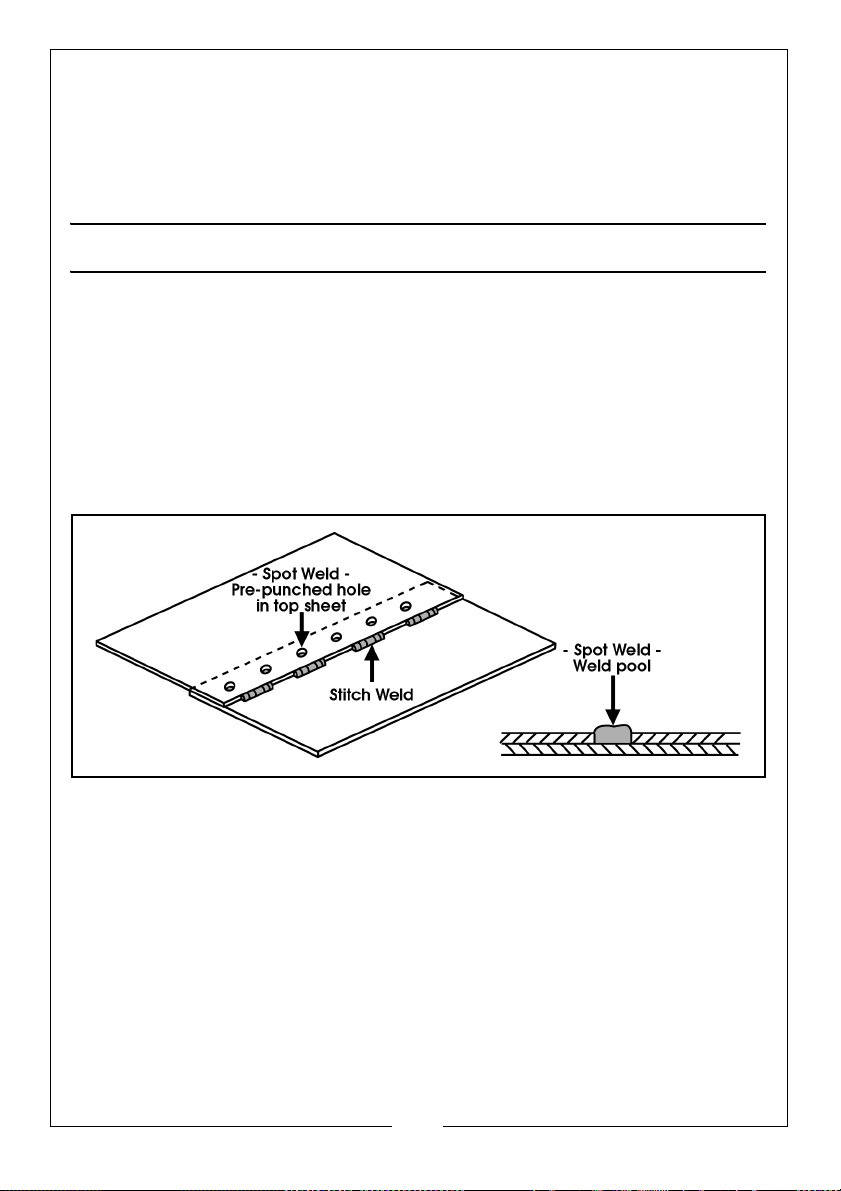
SPOT TIMER CONTROL
This control may be used for spot (plug) welding, or stitch welding. The control
is set so that the duration of weld lasts for a predetermined time.
For plug welding, a special nozzle is required, (see your CLARKE dealer) which
is pressed hard against the two pieces of material to be welded, as the trigger
is pressed. The arc will last for a predetermined time, depending upon the
control setting, melting the metal and fusing the two parts together.
Allow a short period with parts held together before withdrawing the nozzle.
THERMAL OVERLOAD (MIG220TE)
The ‘Thermal Overload’ is a safety device which shuts off the welder when the
duty cycle has been exceeded. This is to prevent damage to the machine
caused by overheating.
When this occurs, the warning lamp will glow (amber). Allow the welder to
cool, until the amber light extinguishes before resuming.
For details of the duty cycle...i.e. the length of time the machine may be used
at a particular welding current, refer to the data and notes on page 24.
24
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 25
BURN BACK ADJUSTMENT
This takes the form of a trimmer, located between the control knobs on the
front panel which can be adjusted with a screwdriver eitther clockwise or anticlockwise.
It is used to regulate the amount of welding wire to “burn back” after releasing
the trigger of the torch. For example, if this is set to Maximum, when the weld is
finished, the wire will burn back almost to the nozzle tip. Initially set the trimmer
to an intermediate setting but this may be adjusted according to the
diameter of wire being used
ACCESSORIES
A full range of accessories is available from your Clarke dealer.
WELDING TIPS
• Try to maintain the tip of the nozzle at an angle of approx. 45O and at a
constant distance of approx 5-7mm from the workpiece.
• Try to maintain a constant speed of movement with the torch.
• Do not weld in windy conditions or in an area where ventilation is a
problem, or where air flow fluctuates.
• ALWAYS keep the wire and nozzle clean...NEVER use rusted wire.
• Avoid sharp bends or kinks in the welding hose.
• Whenever possible, clean out the wire liner with compressed air when
replacing the wire spool.
• Periodically remove the dust, using LOW PRESSURE compressed air, within
the casing. Adequate heat dissipation is essential during the welders
operation.
DUTY CYCLE
These models are covered by regulations EN 60974-1 and EN 50199, where the
Duty Cycle (X) is expressed as a percentage of time the machine may be
used in a given period for a specified welding current.
i.e. using the example below, which is an illustration of the 270TE data plate.....
25
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 26
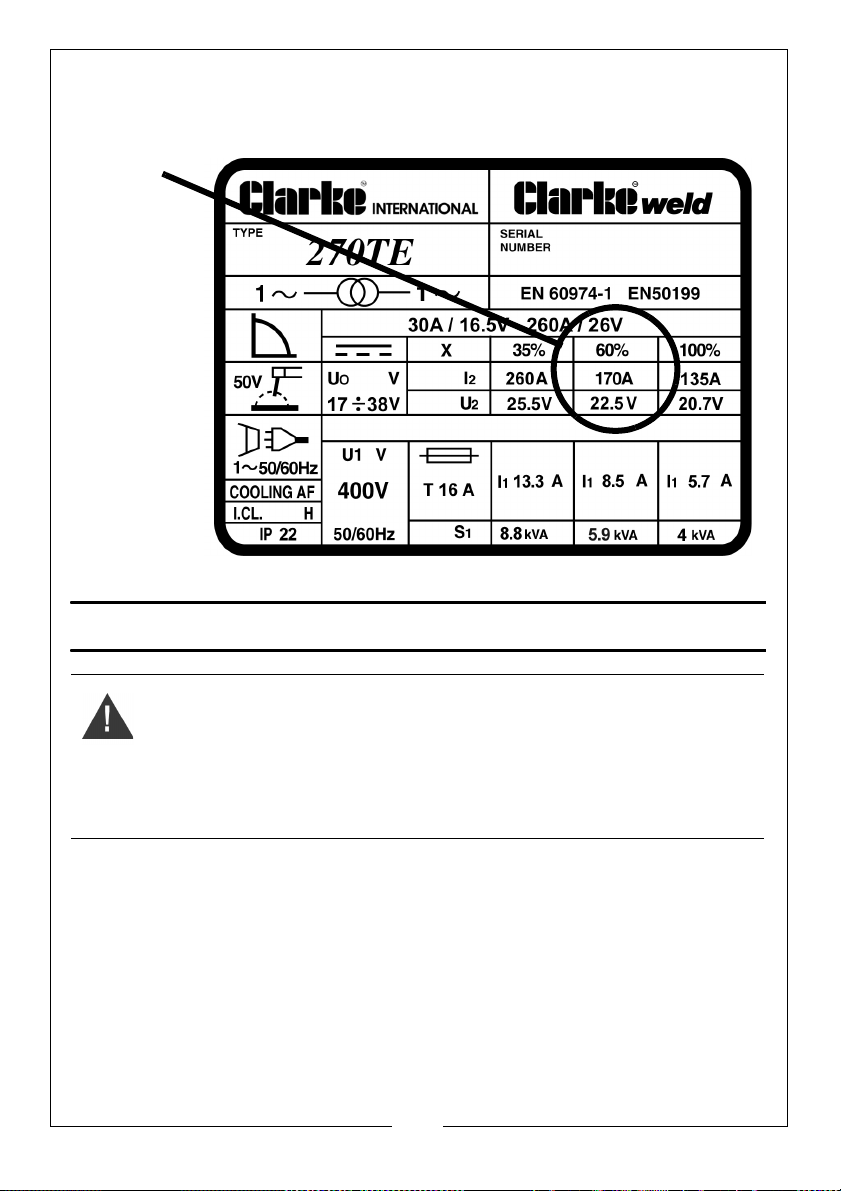
When welding at 170 Amps the machine may be used for 6 minutes (60%) in
any 10 minute period or, the machine may be used continuously, (100%) when
welding at 135 Amps.
MAINTENANCE
WARNING: ELECTRICITY CAN KILL....NEVER TOUCH LIVE ELECTRICAL
COMPONENTS
WARNING: DISCONNECT THE POWER SUPPLY BEFORE ALL INSPECTIONS
AND MAINTENANCE OPERATIONS
WARNING: BEWARE HOT SURFACES.....ALWAYS LET THE POWER SUPPLY
COOL DOWN BEFORE ACCESSING INTERNAL COMPONENTS.
Frequency of maintenance operations depends on the operating conditions,
how intensively the welder is used, and how clean or dirty the welding site is
(aggressive atmospheres, etc).
Always inspect the earth return and torch hose, before use to ensure they are
in perfect condition and earth clamp is clean and secured correctly to the
cable.
Check the gas hose and pressure regulator for security and serviceability, and
ensure there is sufficient gas to complete the job in hand.
As a general rule the power supply should be inspected internally at least
annually. Consult your CLARKE dealer.
26
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 27
THE WELDING SHIELD
Always maintain the welding shield in good condition. If the clear glass
protection lens becomes badly pitted, sufficient to interfere with vision, or
cracked, have it replaced immediately.
Replacement clear and dark lenses are available from your Clarke dealer see Parts Lists for details. NEVER use any dark filter lens other than that
provided by CLARKE International, or one with the same certified ‘Optical
class’ (degree of protection).
The shield should always be cleaned with a clean soft cloth after use, ensuring
the lenses are clean. Remove any dust that may have accumulated and store
it in a safe place where it cannot be damaged. NEVER use a shield that is not
in perfect condition.
27
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 28
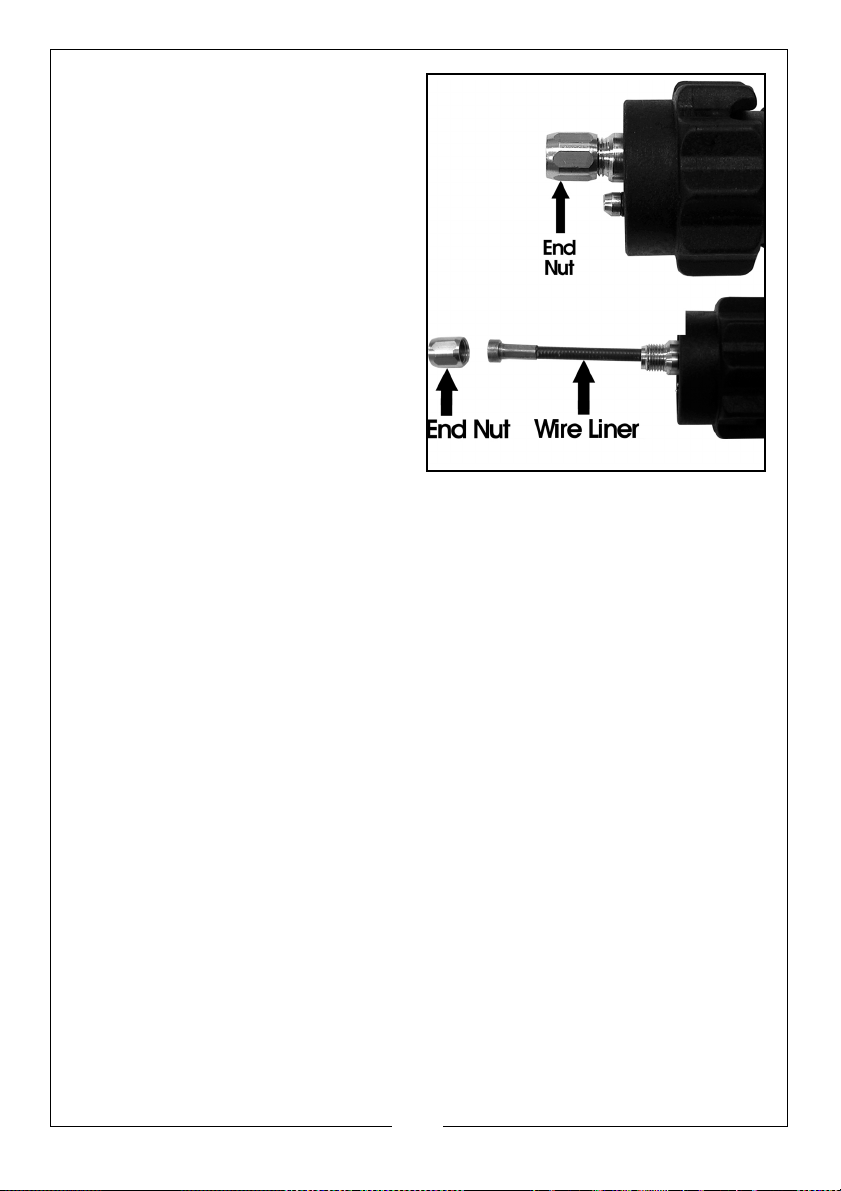
RENEWING THE WIRE LINER
If the liner becomes damaged or
kinked it will be necessary to replace
it.
1. Remove the welding wire from the
hose & torch assembly, either by
cutting it at the wire spool and
pulling through from the nozzle
end, or rewinding it back on the
spool.
2. Disconnect the hose from the
machine.
3. Unscrew the end not shown in Fig
11 using a 12mm spanner and
having straightened the hose
assembly, pull the liner completely
out of the hose.
4. Thread the new liner into the hose fully, then screw the end nut back into
place.
28
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 29
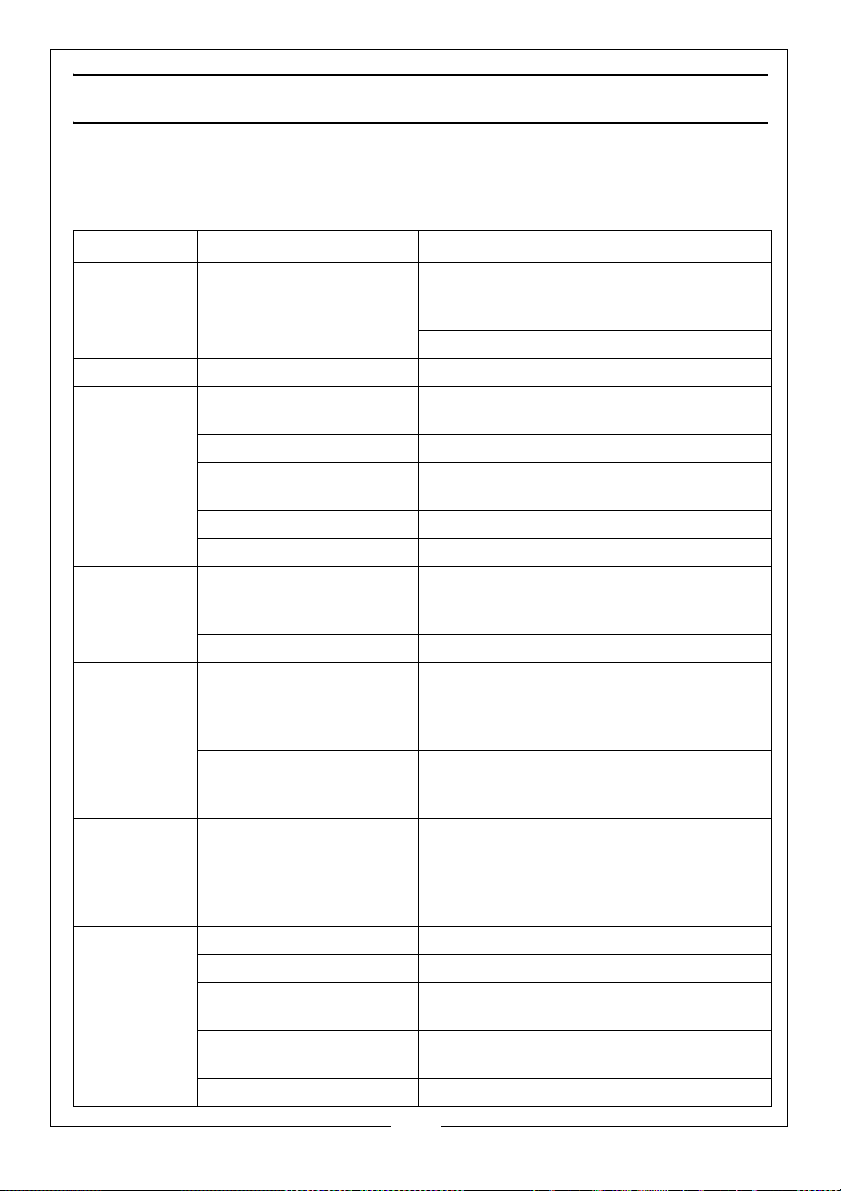
TROUBLESHOOTING
Your Clarke Mig Welder has been designed to give long and trouble free service.
If, however, having followed the instructions in this booklet carefully, you still
encounter problems, the following points should help identify and resolve them.
CAUSE REMEDY
No “life” from
welder
No wire feed Motor malfunction Return welder to your local dealer
Feed motor
operates but
wire will not
feed
Wire welds
itself to tip
Wire feeds
into ‘birds
nest’ tangle
Loose coils of
wire tangle
around wire
drum inside
machine
Erratic wire
feed
Check fuses and mains
lead
Insufficient Feed Roller
Pressure
Burr on end of wire Re-cut wire square with no burr
Liner blocked or damaged Clean with compressed air or
Inferior wire Use only good “clean” wire
Roller worn out Replace roller
Wire feed speed too low Unscrew tip, cut wire and fit new tip
Wrong size tip Fit correct size tip
Wire welded to tip As above plus reduce feed roller
Wire liner damaged
preventing smooth
operation
Drum brake too slack Tighten drum brake Caution: Do not over-
Drum brake too tight Loosen drum brake slightly
Feed roller worn Check and replace if necessary
Insufficient pressure on
feed roller
Wire dirty, rusty, damp or
bent
Liner partially blocked Clean with compressed air
Replace fuses as necessary If
problem persists return welder to your local
dealer
Check fuse size
Increase roller pressure
replace liner.
Increase wire speed before
operating again
nest’ tangle pressure so that if blockage
occurs
wire slips on roller i.e. no feed
Renew wire liner
tighten
Increase pressure on feed roller
Caution: Do not over-tighten
Re-cut wire and ensure it is clean
29
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 30
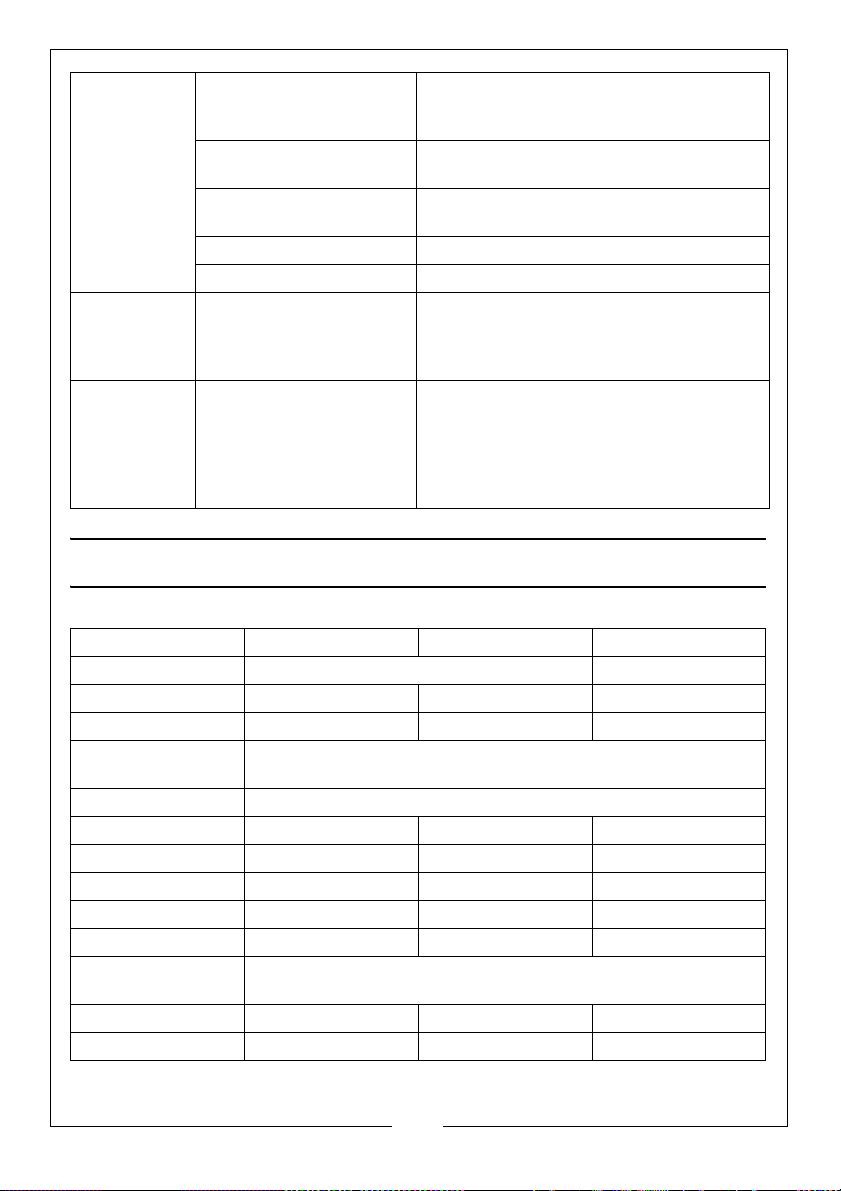
Poor quality
welds
Wire jams in
tip when
welding
aluminium
Welder cuts
out whilst in
use
Insufficient gas at weld
area
Incorrect gas/wire
combination
Rusty, painted, damp, oil
or greasy workpiece
Rusty/dirty wire Ensure wire is clean and dry
Poor earth contact Check earth clamp/work onnection.
Tip too small Use slightly oversize tip ie., for 0.8mm wire
Duty cycle exceeded
(auto cut-out operates)
Check that gas is not being blown away by
draughts and if so move to more sheltered
weld area. If not increase gas supply
Consult your MIG welding manual for
correct set-up
Ensure workpiece is clean and dry
use 1mm tip. (Note: Applies to aluminium
only)
Allow welder to cool 15-30 mins before
continuing
Note: If duty cycle is continually
exceeded, damage to the welder may
result, and welder output is probably too
small for application.
SPECIFICATIONS
220TE TURBO 255TEC TURBO 270TE TURBO
Power Supply 230V 50Hz 1Ph 400V 50Hz 3Ph
Main Fuse Rating 25 Amps 40 Amps 16 Amps
Current Range 40-200A 30-250A 30-260A
Max. Metal Thickness
(m/s)
Welding Wire Sizes 0.6-0.8mm
Duty Cycle* 20% 200A
30% 250A
35% 260A
60% 123A 150A 170A
100% 95A 140A 135A
Dimensions (no
handle) mm
Weight 71 kg 79 kg 79 kg
Part No. 6015220 6015510 6015240
10-11mm
740x830x500
* Duty Cycle: Determines the machine ‘down time’.
30
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 31
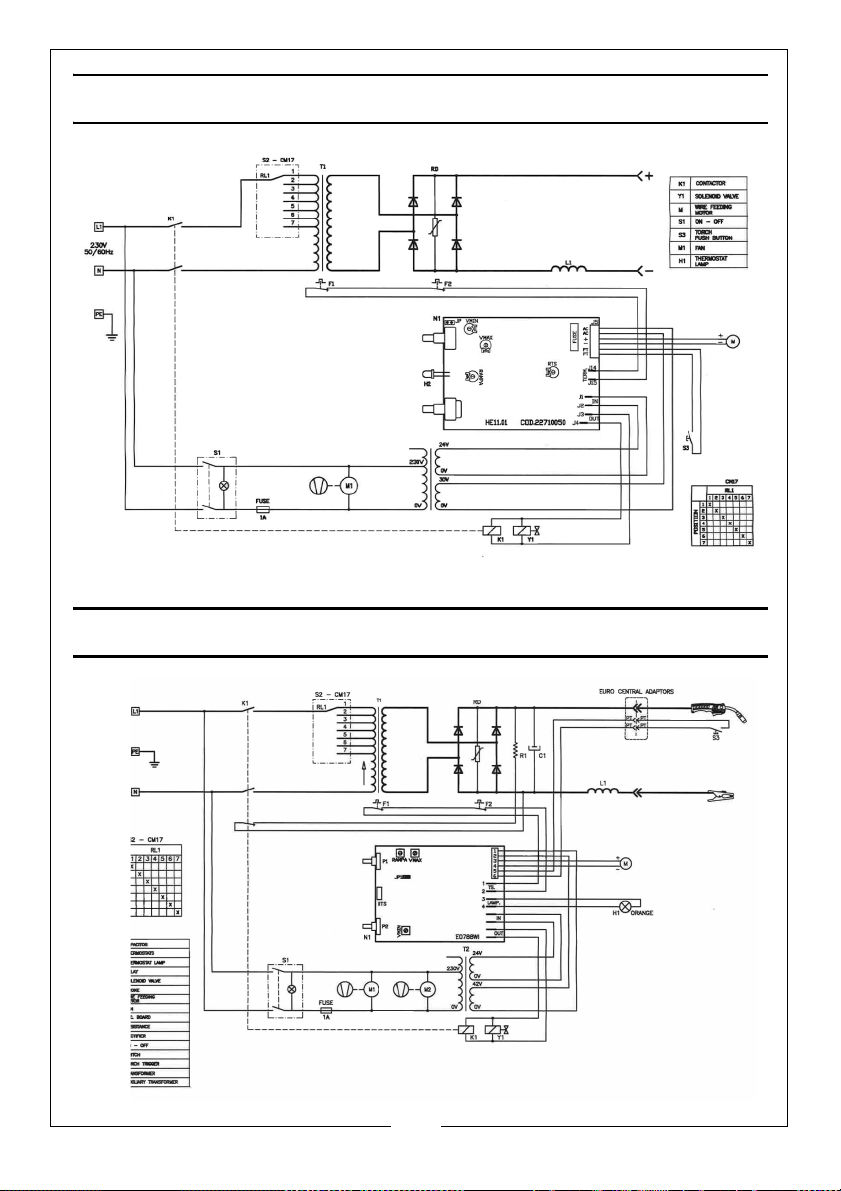
WIRING DIAGRAM - MIG220TE
WIRING DIAGRAM - MIG255TEC
31
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 32
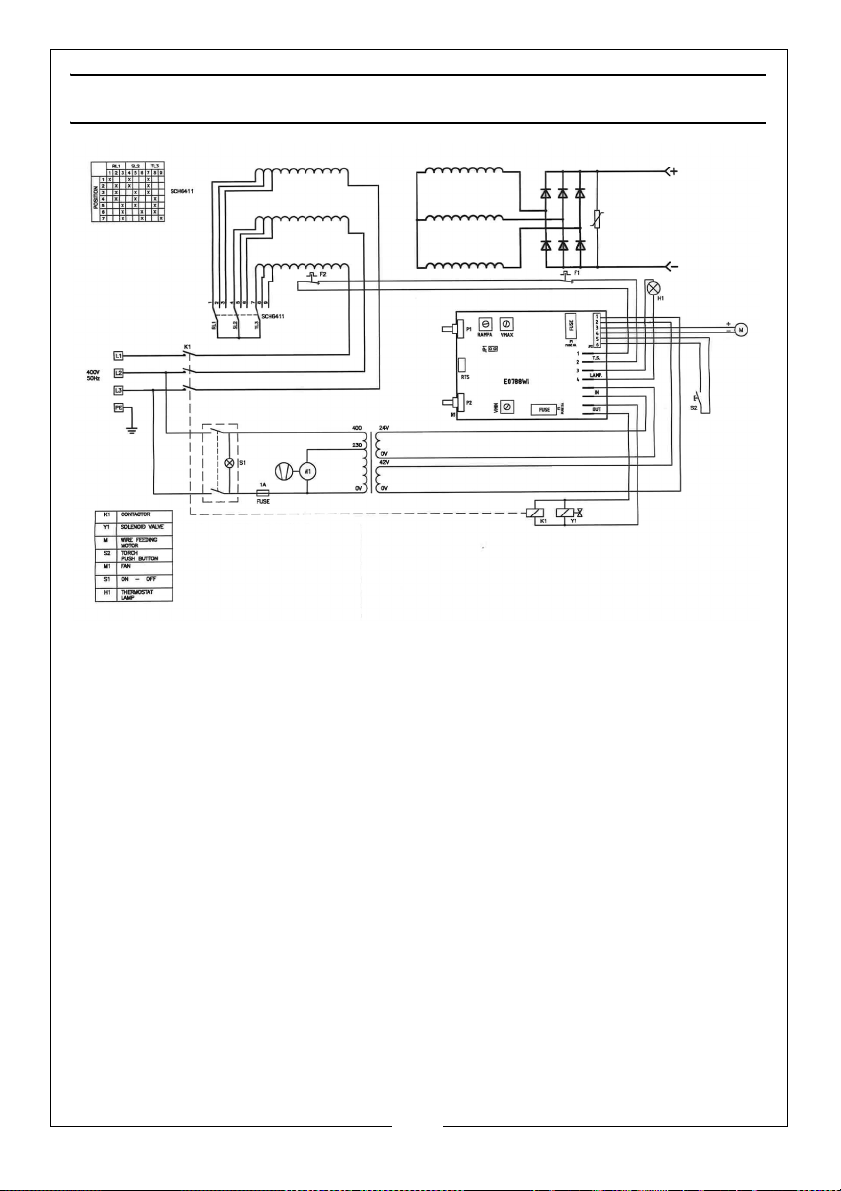
WIRING DIAGRAM - MIG270TE
32
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 33
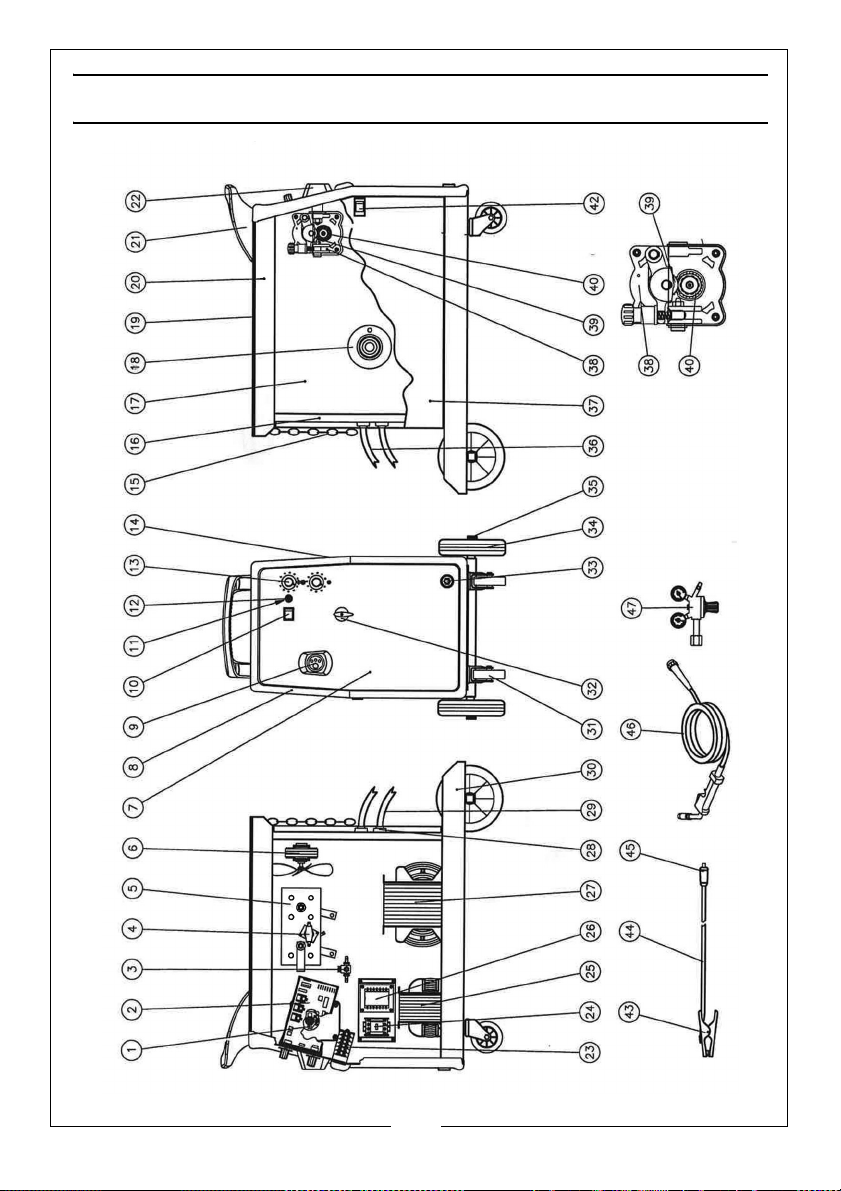
PARTS DIAGRAM - MIG220TE
33
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 34
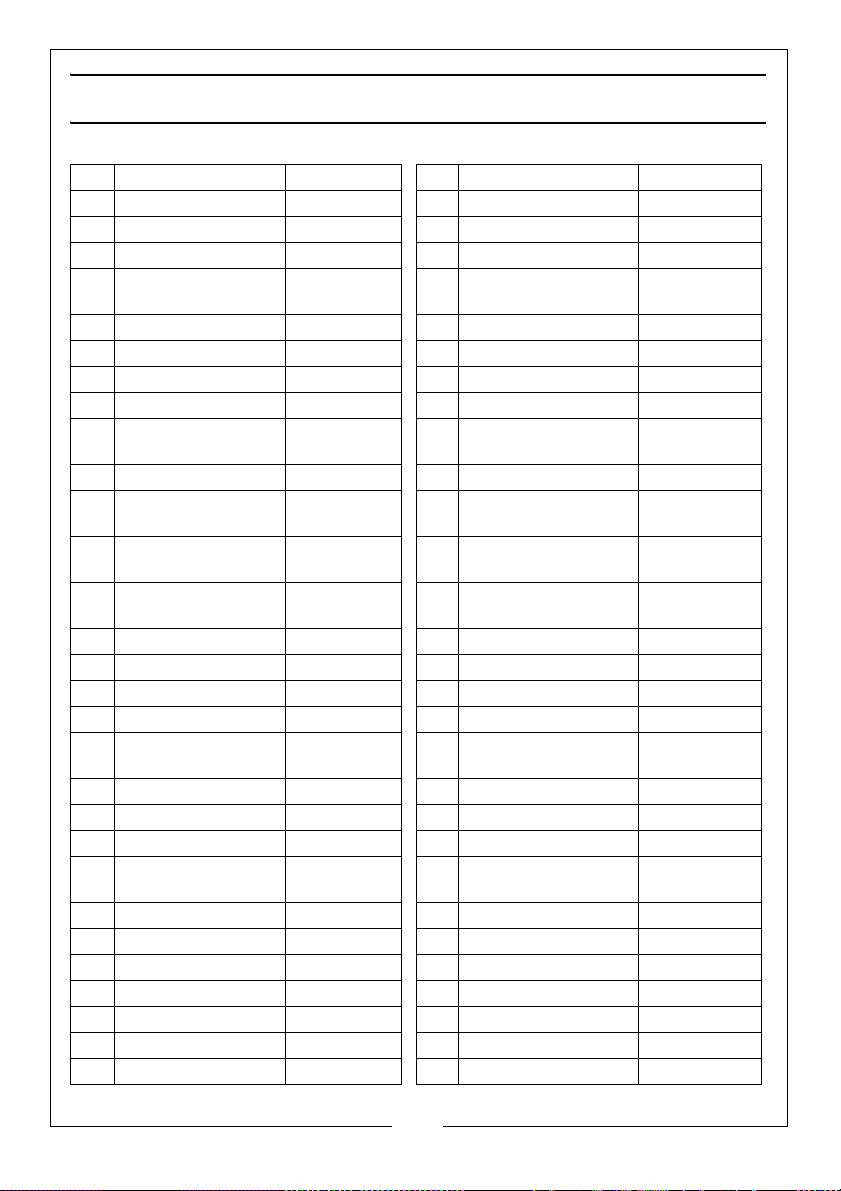
PARTS LIST - MIG220TE
No. Description Part No. No. Description Part No.
01 Motor + Pinion EM04600147 30 Lower Panel EM33700317
02 Motor Control PCB EM22710190 31 Castor EM21625003
03 Gas Solenoid Valve EM22900035 32 Switch Knob EM21690268
04 Thermostat +
Support
05 Rectifier EM22400085 34 Rear Wheel EM21625048
06 Fan 220V EM22800002 35 Wheels Axle EM55200036
07 Front Panel EM33710295 36 Black Hose EM30900027
08 Plastic Front Frame EM21690285 37 Left Access Panel EM33705627
09 Binzel / Euro Torch
Adaptor
10 On/Off Switch EM22200002 39 Wire Block Roll EM33805007
11 Fuse 1A 250V EM22220002 40 Wire Feed Roll 0,6-
12 Fuse Holder EM22220016 40 Wire Feed Roll 1,0-
13 Potentiometer Knob EM04600332 40 Wire Feed Roll 0,8-
14 Right Side Panel EM33705326 42 Slide Clip EM21690226
15 Zinc Chain EM04600205 43 Earth Clamp 300A EM22110033
16 Rear Panel EM33715096 44 Earth Cable EM43210167
17 Dividing Panel EM33720211 45 Dinse Plug EM22100001
18 Complete Spool
Holder
19 Tool Mat EM30905045 47 Reducer c/w Gauge EM22905017
20 Upper Panel EM33705628 49 Mask EM21905029
21 Handle EM21600042 50 Clear Glass EM21905020
22 Torch Connection
Cover
23 Switch 20A EM22205033
24 24V Contactor EM22225022
25 Choke EM44135082
26 Auxiliary Transformer EM44140054
27 Transformer EM44120109
28 Cable Clamp EM21605010
29 Input Cable EM20220020
EM04600113 33 Female Dinse Plug EM22100002
EM23005048 38 Aluminium Wire
Feeder + Gear
0,8mm
1,2mm
1mm
EM04600275 46 Torch EM23000424
EM21690267 51 Dark Glass EM21905024
EM44410021
EM33805003
EM33805005
EM33805104
34
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 35
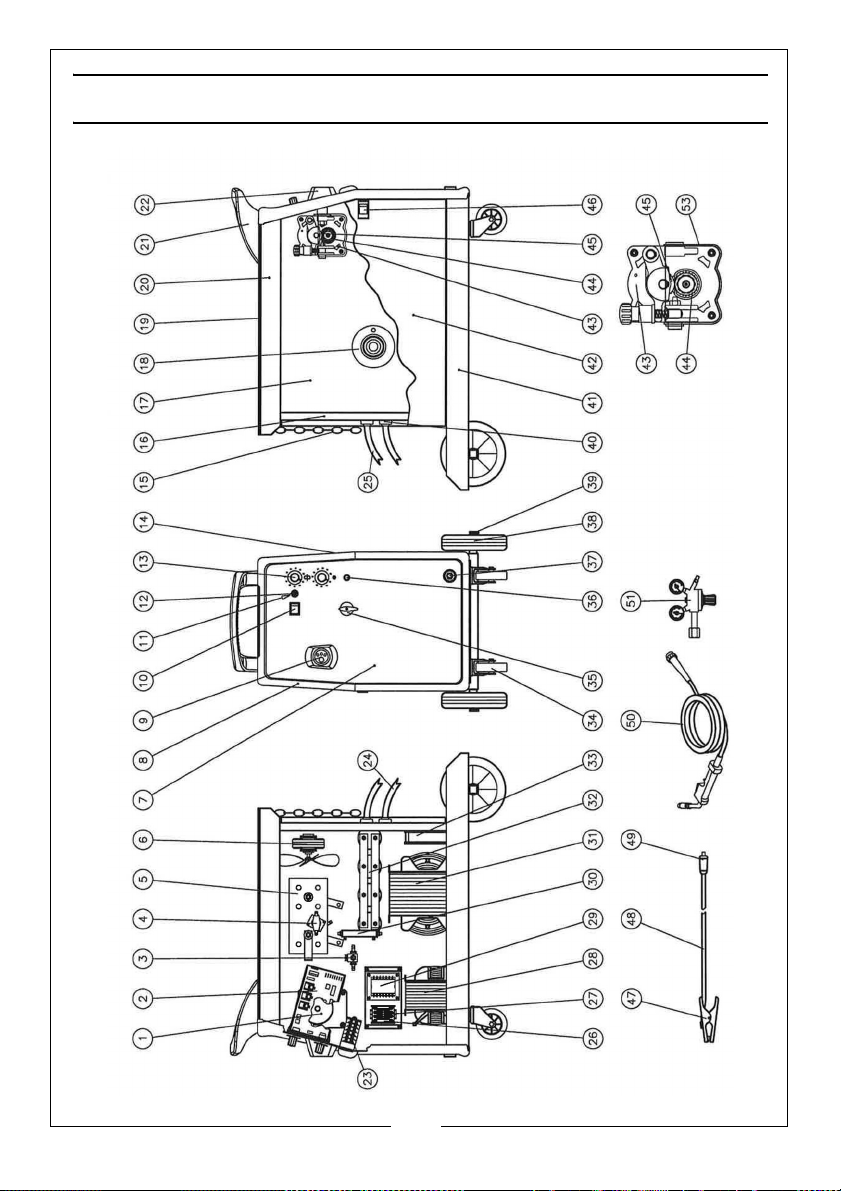
PARTS DIAGRAM - MIG255TEC
35
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 36
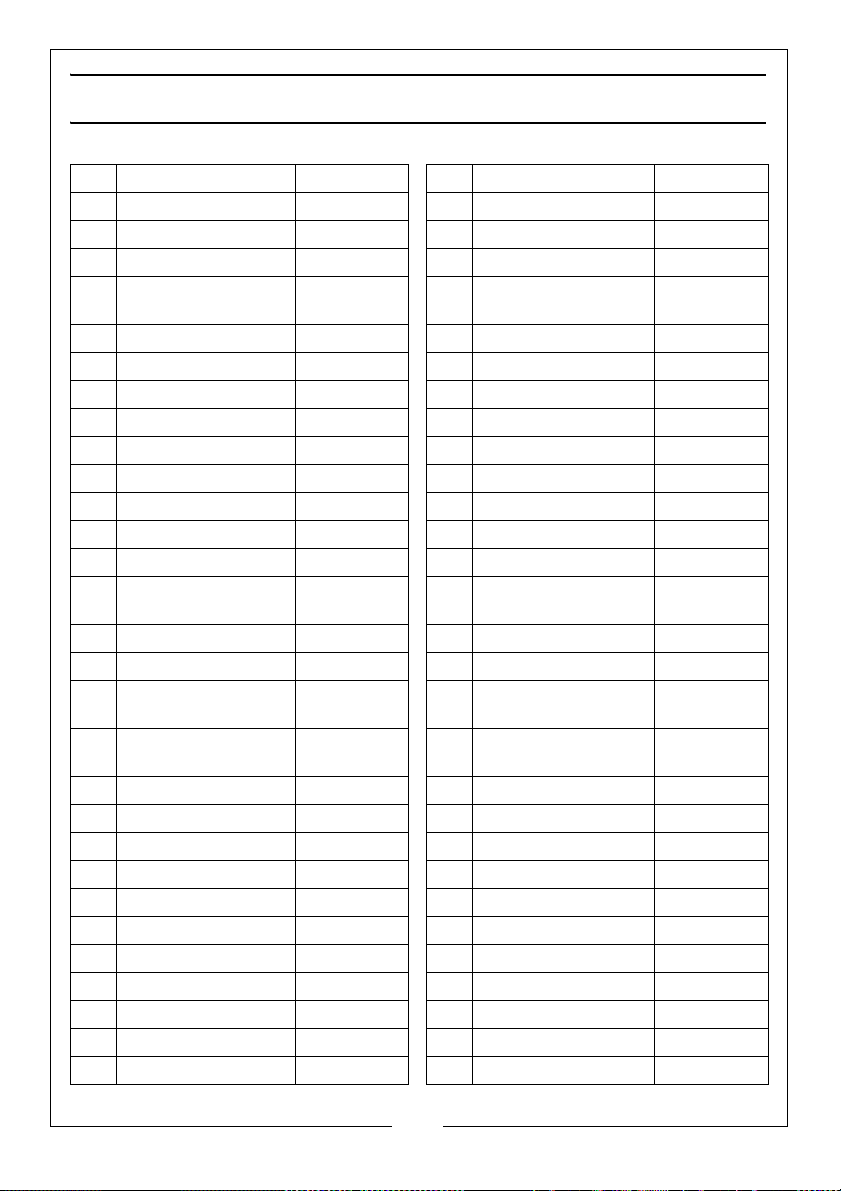
PARTS LIST - MIG255TEC
No. Description Part No. No. Description Part No.
1 Wire Feed Motor 42V EM22810006 30 Resiistor EM22305004
2 P.C. Board EM22710051 31 Transformer EM44120147
3 Gas Solenoid Valve EM22900035 32 Capacitor EM22315003
4 Complete
Thermostat
5 Rectifier EM22400086 34 Castor EM21625003
6 Fan EM22800002 35 Switch Knob EM04600268
7 Front Panel EM33710295 36 Orange Pilot-lamp EM22610011
8 Plastic Front EM21690285 37 Female Plug EM22100002
9 Torch Adaptor EM23005048 38 Rear Wheel EM21625048
10 On/Off Switch EM22200002 39 Wheels Axle EM55200036
11 Fuse EM22220002 40 Cable Clamp EM21605010
12 Fuse Holder EM22220016 41 Lower Panel EM33700317
13 Potentiometer Knob EM04600332 42 Left Access Panel EM33705627
14 Right Side Panel EM33705626 43 Aluminium wire
15 Chain EM04600205 44 Feed Roll 0.6-0.8mm EM33805003
16 Rear Panel EM33715096 44 Feed Roll 1.0-1.2mm EM33805005
17 Dividing Panel EM33720211 44 Feed Roll 0.8-1.0mm
18 Complete Spool
Holder
19 Mat For Tools EM30905045 45 Block Roll EM33805007
20 Cover Panel EM33705628 46 Slide Clip EM21690226
21 Handle EM21600042 47 Earth Clamp EM22110033
22 Torch Connect Cover EM21690267 48 Earth Cable EM43210167
23 Switch EM22205155 49 Dinse Plug EM22100001
24 Input Cable EM20220136 50 Torch EM23000424
25 Black Gas Hose EM30900027 51 Reducer EM22905017
26 Contactor EM22225022 - - Face mask EM21905019
27 Auxiliary Contacts EM22225018 - - Transparent Glass EM21905020
28 Choke EM44135128 - - Dark Glass EM21905024
29 Auxiliary Transformer EM44140054
EM04600113 33 Complete Fan EM22800021
EM44410017
Feeder
nylon
EM04600275 44 FeedRoll1.2-
1.6mmnylon
EM33805104
EM33805105
36
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 37
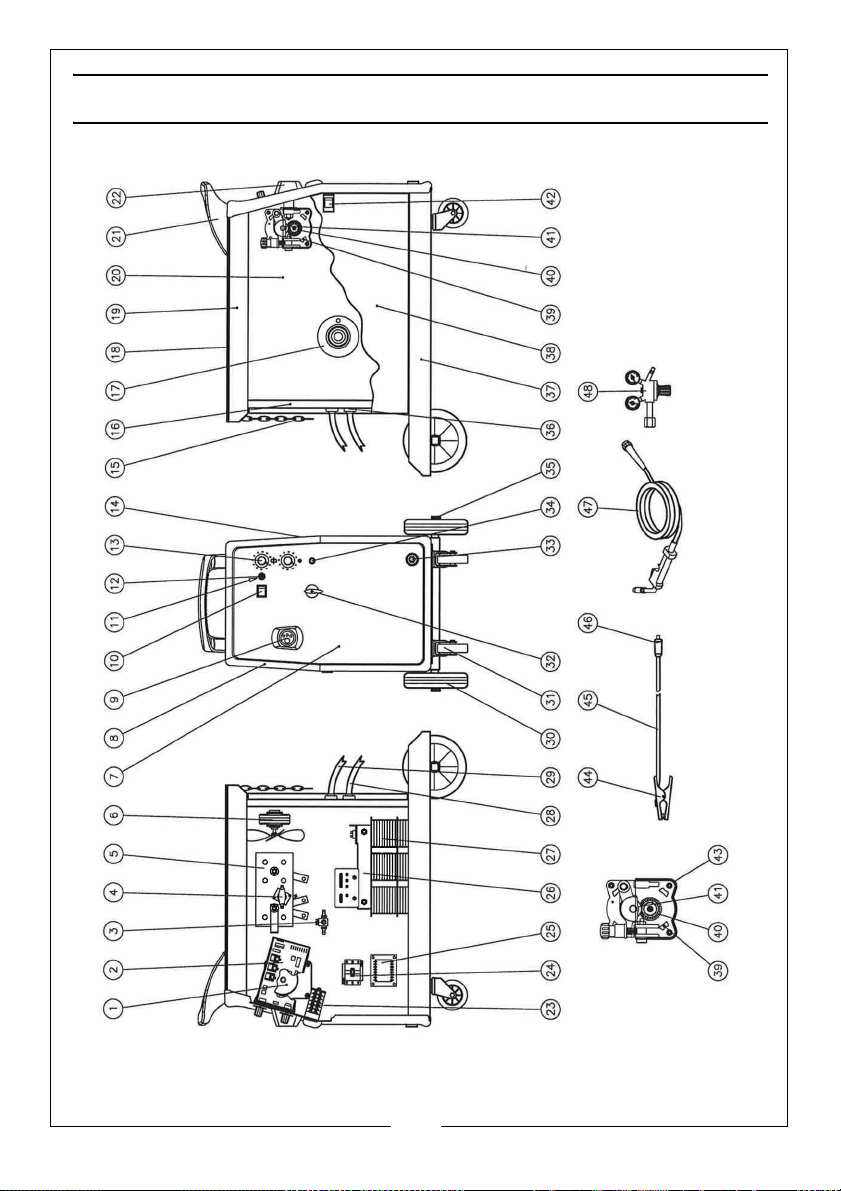
PARTS DIAGRAM - MIG270TE
37
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 38
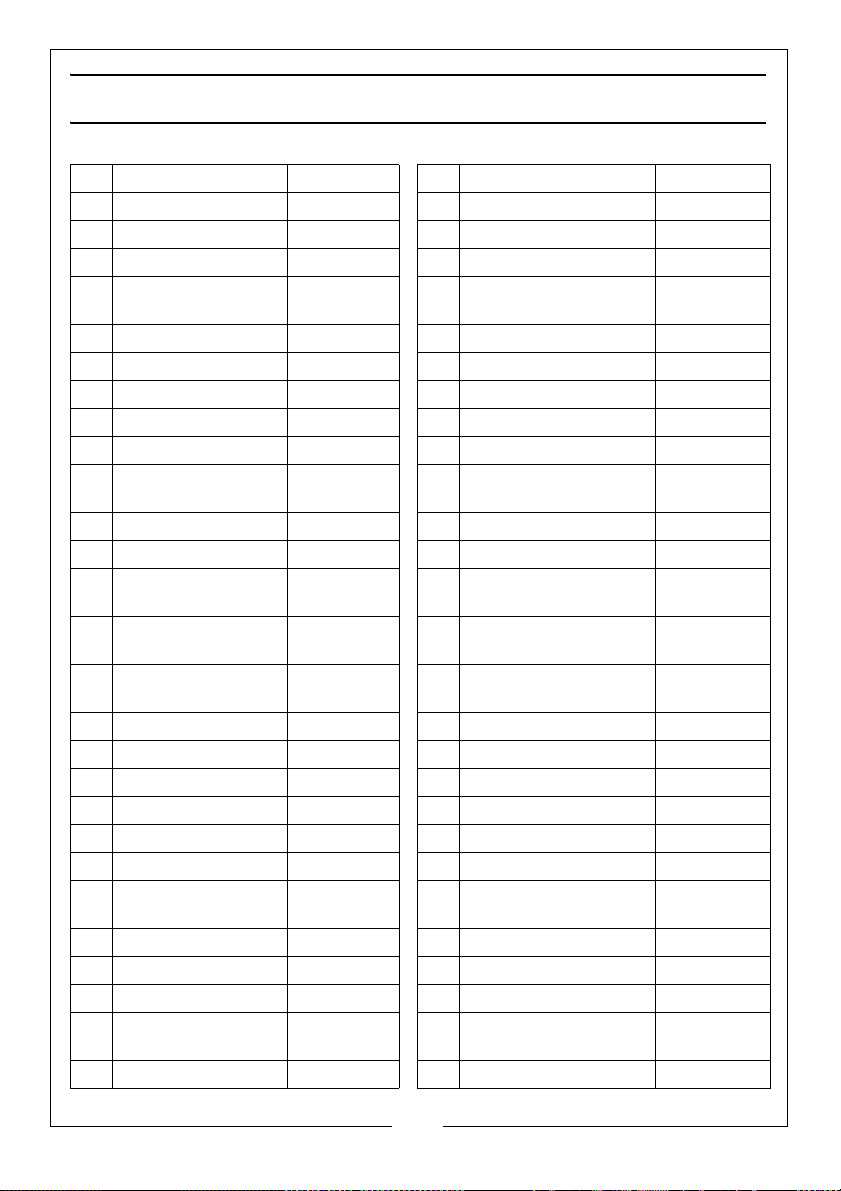
PARTS LIST - MIG270TE
No. Description Part No. No. Description Part No.
1 Wire Feed Motor 42V EM22810006 28 Input Cable EM20220030
2 P.C. Board EM22710051 29 Black Hose EM30900027
3 Gas Solenoid Valve EM22900035 30 Rear Wheel EM21625048
4 Thermostat +
Support
5 Rectifier EM22400029 32 Switch Knob EM04600268
6 Fan EM22800005 33 Female Dinse Plug EM22100002
7 Front Panel EM33710295 34 Orange Pilot-lamp 24V EM22610011
8 Front Frame EM21690285 35 Wheels Axle EM55200036
9 Euro Torch Adaptor EM23005048 36 Cable Clamp EM21605010
10 Green Pilot-light
Switch
11 Fuse 1A 250V EM22220002 38 Left Access Panel EM33705627
12 Fuse Holder 3A 250V EM22220016 39 Al.. Wire Feeder +Gears EM44410017
13 Potentiometer Knob EM04600332 40 Wire Feed Roll 0,6-
14 Right Side Panel EM33705626 40 Wire Feed Roll 1,0-
15 Zinc Chain 0,76 Mt EM04600205 40 Wire Feed Roll 0,8-1mm
16 Rear Panel EM33715096 41 Wire Black Roll EM33805007
17 Compl. Spool Holder EM04600275 42 Slide Clip EM21690226
18 Mat For Tools EM30905045 --- --- - - - - - - - - -
19 Upper Panel PVC EM33705628 44 Earth Clamp 300A EM22110033
20 Dividing Panel PVC EM33720211 45 Earth Cable EM43210167
21 Handle EM21600042 46 Dinse Plug EM22100001
22 Torch Connection
Cover
23 Switch 16 A EM22205030 48 Reducer 2/Gauges EM22905018
24 Contactor EM22225022 --- Face Mask EM21905029
25 Auxiliary Transformer EM44140036 --- Transparent Glass EM21905020
26 Transformer 230/
400V
27 Al Side Winding 230V EM44025084
EM04600113 31 Castor EM21625003
EM22200005 37 Lower Panel EM33700317
EM33805003
0,8mm
EM33805005
1,2mm
Nylon
Nylon
EM21690267 47 Torch-bl/blk Handle EM23000424
EM44125038 --- Dark Glass EM21905024
EM33805104
38
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 39
DECLARATION OF CONFORMITY
39
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 40
 Loading...