

Page 1
Page 2
Holemaking
High-Performance Taps...........................................................................................................................................................A4–A140
Solid Carbide Taps • GX Series .....................................................................................................................................A6–A29
HSS-E-PM Taps • GT Series.......................................................................................................................................A30–A85
HSS-E Taps • EM Series ...........................................................................................................................................A86–A140
Production Taps ...................................................................................................................................................................A142–A196
Maintenance Tools...............................................................................................................................................................A198–A213
Maintenance Taps ...................................................................................................................................................A198–A204
Dies.........................................................................................................................................................................A205–A209
Accessories.............................................................................................................................................................A210–A211
Maintenance Sets....................................................................................................................................................A212–A213
High-Performance Thread Mills • GTM Series..................................................................................................................A214–A238
Solid and Indexable Thread Mills........................................................................................................................................A239–A245
Technical Information ..........................................................................................................................................................A248–A274
Solid Carbide Drills ..............................................................................................................................................................A276–A357
VariDrill....................................................................................................................................................................A276–A309
TOP DRILL S for Steel and Cast Iron.......................................................................................................................A310–A333
TOP DRILL S+ ........................................................................................................................................................A334–A338
TOP DRILL G for Non-Ferrous Materials..................................................................................................................A340–A357
Modular Drills........................................................................................................................................................................A359–A362
Spade Blade Holders............................................................................................................................................................A364–A370
Straight Shanks.......................................................................................................................................................A364–A366
Taper Shanks ..........................................................................................................................................................A367–A370
Spade Blades ........................................................................................................................................................................A371–A377
WWW.WIDIA.COM
A3
Page 3
New Products
Our latest metalcutting advances are designed to deliver higher productivity, longer
tool life, and increased application versatility compared with your current tooling.
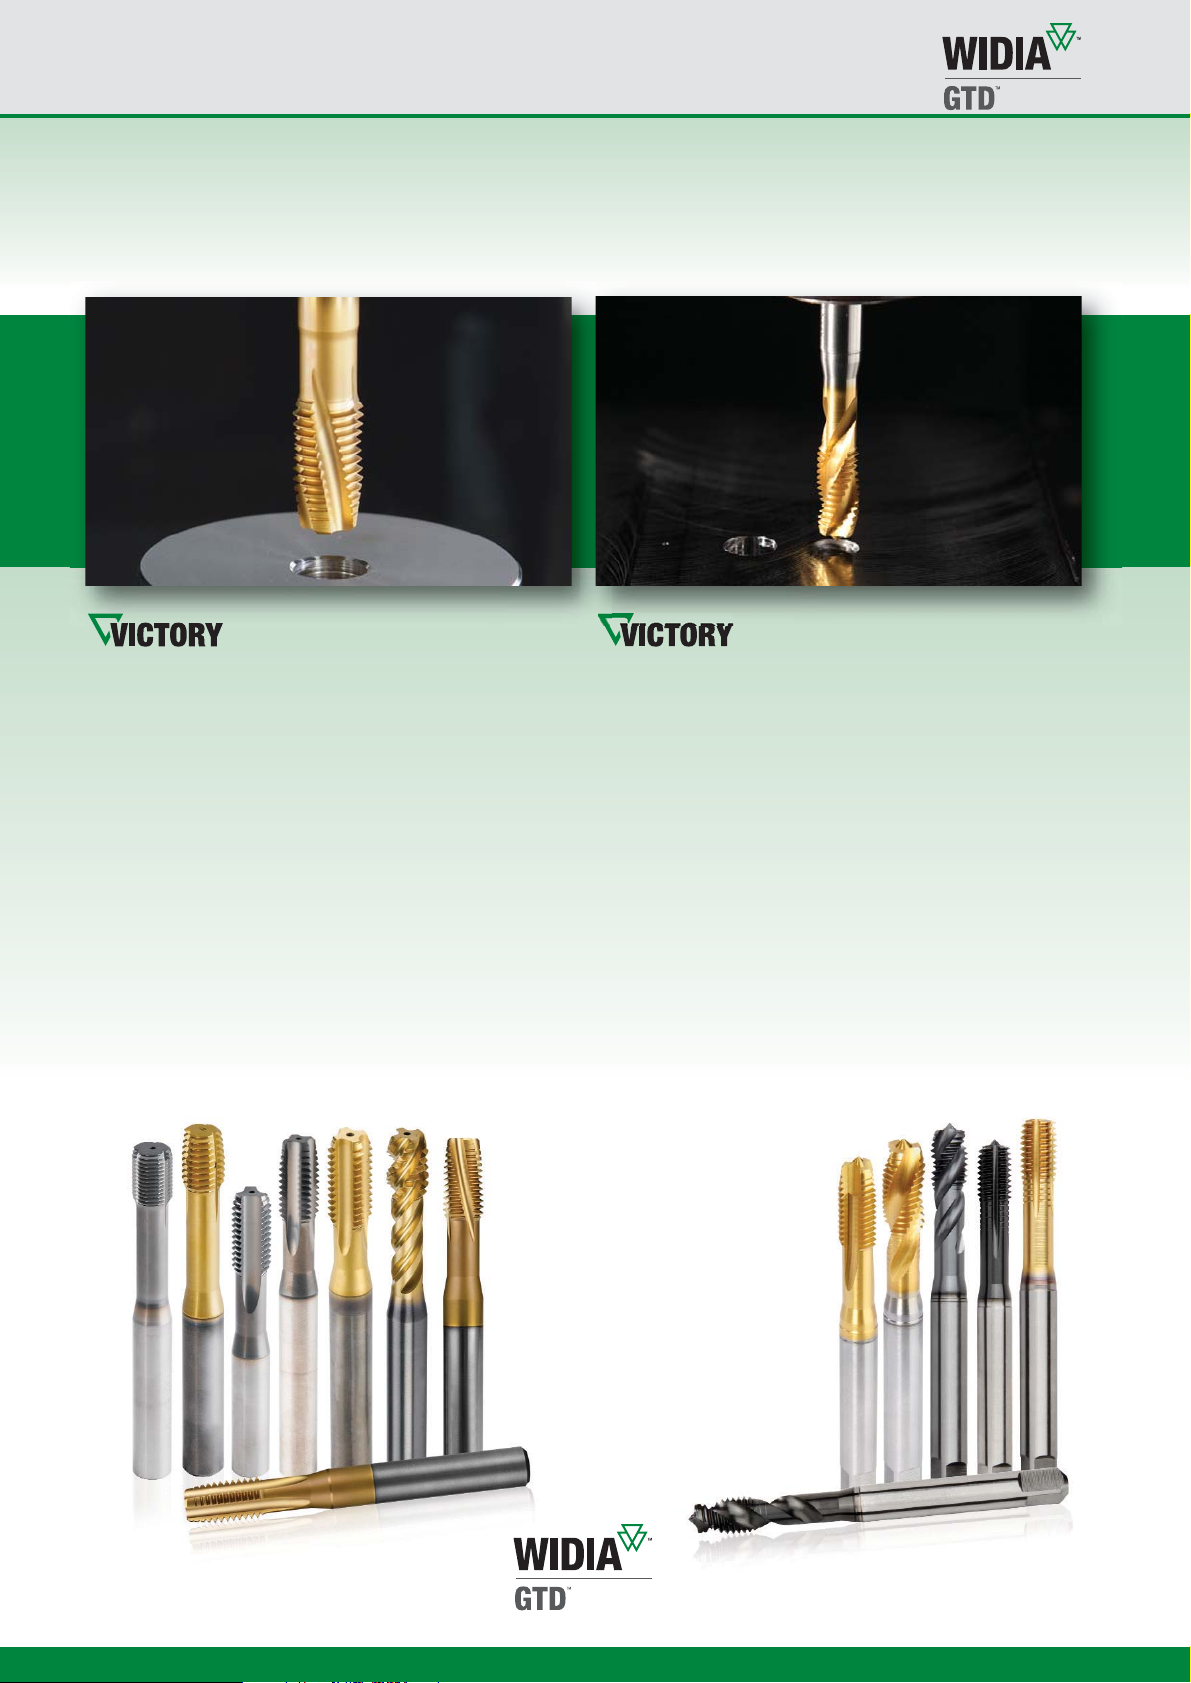
Victory™GX Series Taps Victory
• Our best-performing, high-precision solid carbide taps.
• Run up to 4x faster and last up to 4x longer than
conventional high-speed steel taps.
• Precision design delivers more accurately tapped holes.
• Cutting taps can be factory reconditioned to original
patented specifications and tolerances.
• New generation of high-performance, high-speed steel
powdered-metal taps for material-specific tapping
applications.
• Optimum combination of grades, geometries, and coatings
to deliver higher quality threads and longer tool life.
• Boost your productivity with our unique, highly
wear-resistant powder-metal substrate, modified
with a higher than standard cobalt content for greater
heat resistance.
GT Series Taps
A4
WWW.WIDIA.COM
Page 4
For more information about the latest products and services
from WIDIA, please contact your WIDIA Representative
or Authorized WIDIA Distributor, or visit www.widia.com.
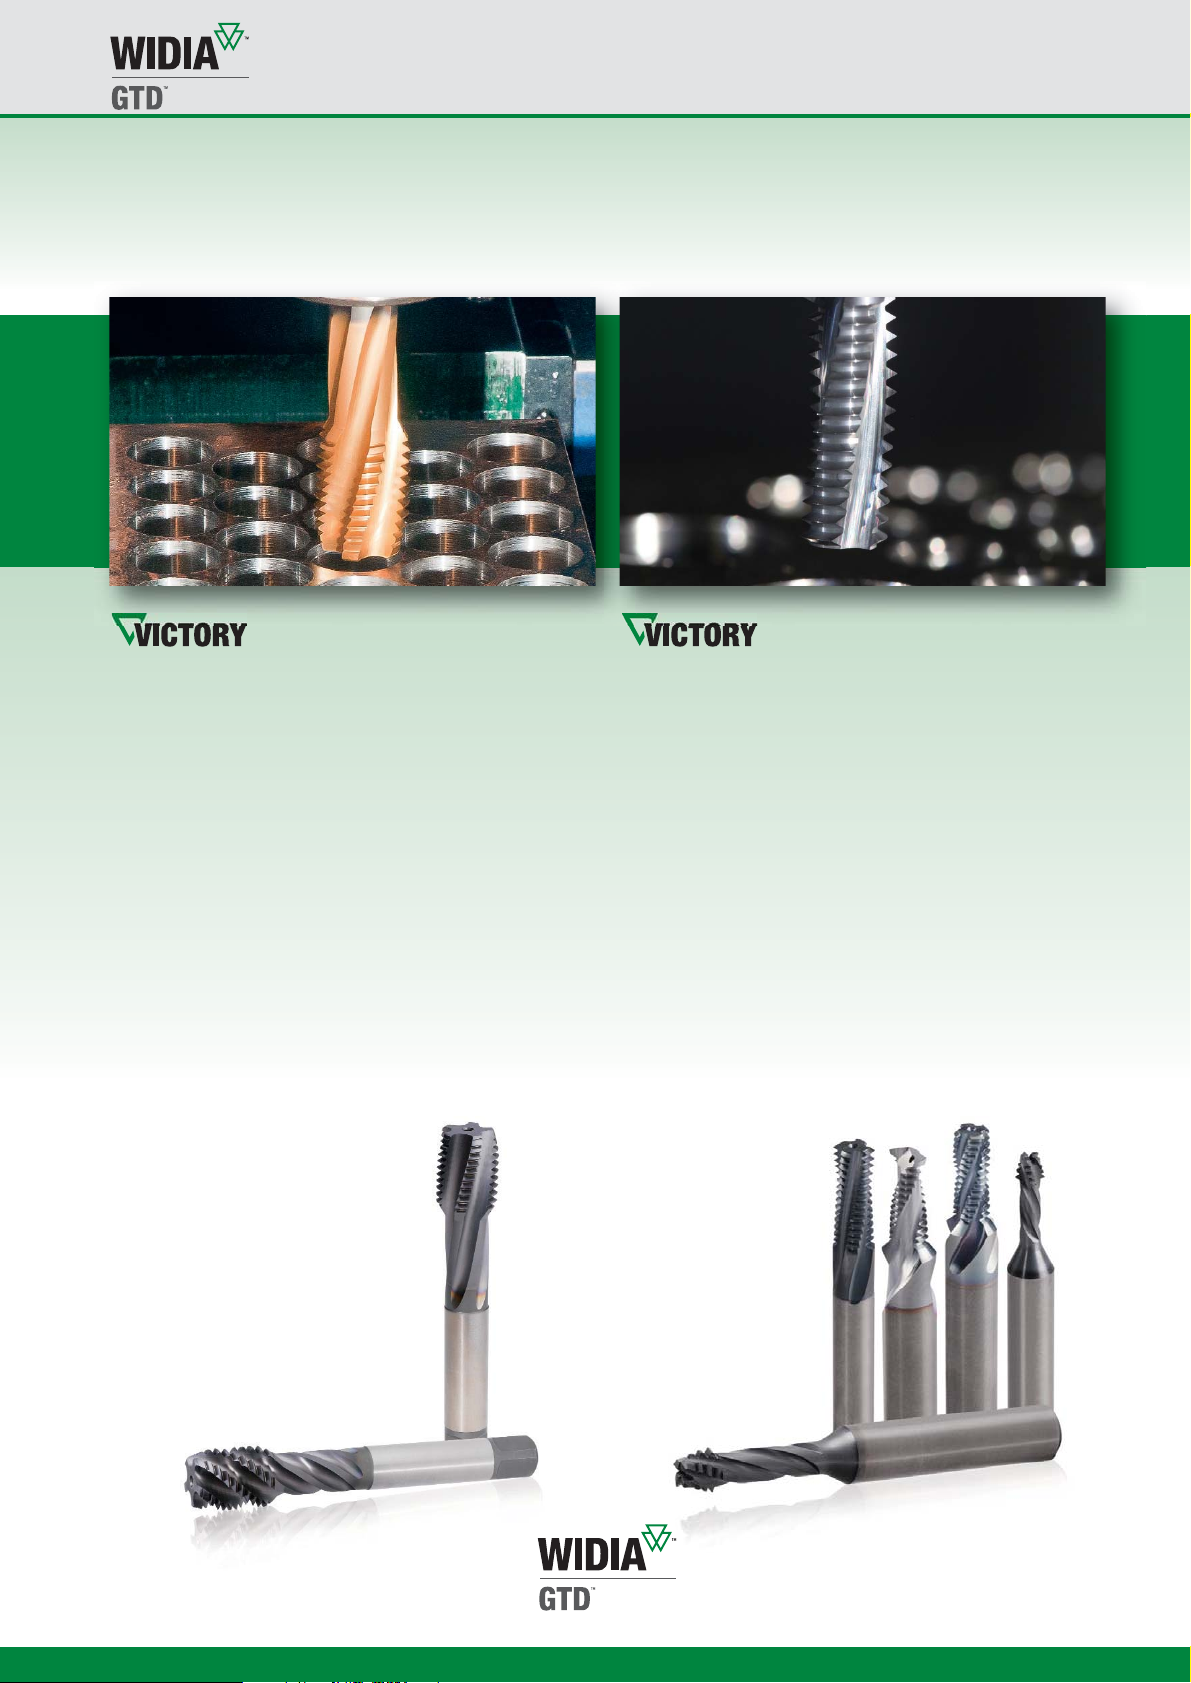
Victory™ GT Series Wind Taps
• New high-performance, large-sized HSS-E-PM taps.
• Developed for manufacturing important wind turbine
components like hubs, rings, and gearbox housing.
• For both conventional non-rigid and CNC-synchronous
tapping machines.
• Can be used with precision round- or square-drive
toolholders.
• An extra-long version is also available.
Victory
• The new high-performance solid thread mills program
is designed for maximum performance and reliability.
• Internal or external thread on 3-axis CNC machining.
• Produce thread on broad range of materials up to 63 HRC.
• GTM31 and GTM41 can drill the hole, countersink the
hole, and cut the thread all at the same time, resulting
in shorter cycle time and fewer tool changes.
• Short chips enable better evacuation and secure
performance.
GTM Series Thread Mills
WWW.WIDIA.COM
A5
Page 5
High-Performance Solid Carbide Taps
Solid carbide taps for high productivity and outstanding performance
in a wide range of workpiece materials.
WIDIA-GTD
• High performance to surpass competitive taps.
• More production from a single tool.
• Available in various specifications.
Optimized flute design
Better chip evacuation.
Chamfer design
Helps chip load,
lower torque.
™
Carbide substrate
Higher heat resistance,
higher speed.
A6
Various multilayer coatings
Extremely high wear resistance,
longer tool life.
Cylindrical h6 shank
Low runout, higher
quality threads.
WWW.WIDIA.COM
Page 6
Advanced WIDIA™Technology
• Manufactured with fine-grain micrograin carbide
for exceptional wear life.
• Ideal for long production runs where fewer tool changes
mean greater productivity.
• Designed for outstanding tool life in steel, cast iron, aluminum,
and hardened materials.
Features
• Runs 5x faster and lasts 4x longer than conventional taps.
• Enhanced tap precision and design.
• Tap runout less than 10 microns (.0004").
• PVD nanolayer TiAlN/TiN coated carbide grade.
• Custom solutions available upon request.
Benefits
• Superior accuracy of product thread.
• Excellent thread quality and tap performance.
• High edge strength and wear resistance.
• Maximum chip control and free cutting in through holes.
• Can be factory reconditioned to original specifications and tolerances.
Application Information
• For use on CNC machines with synchronous or rigid tapping control
and precision toolholders.
• Straight-flute taps for sizes M16 and larger for ductile or cast iron.
• Use with machining centers equipped with precise and rigid hydraulic,
shrink fit, or precision collet toolholders.
WWW.WIDIA.COM
A7
Page 7
High-Performance Taps
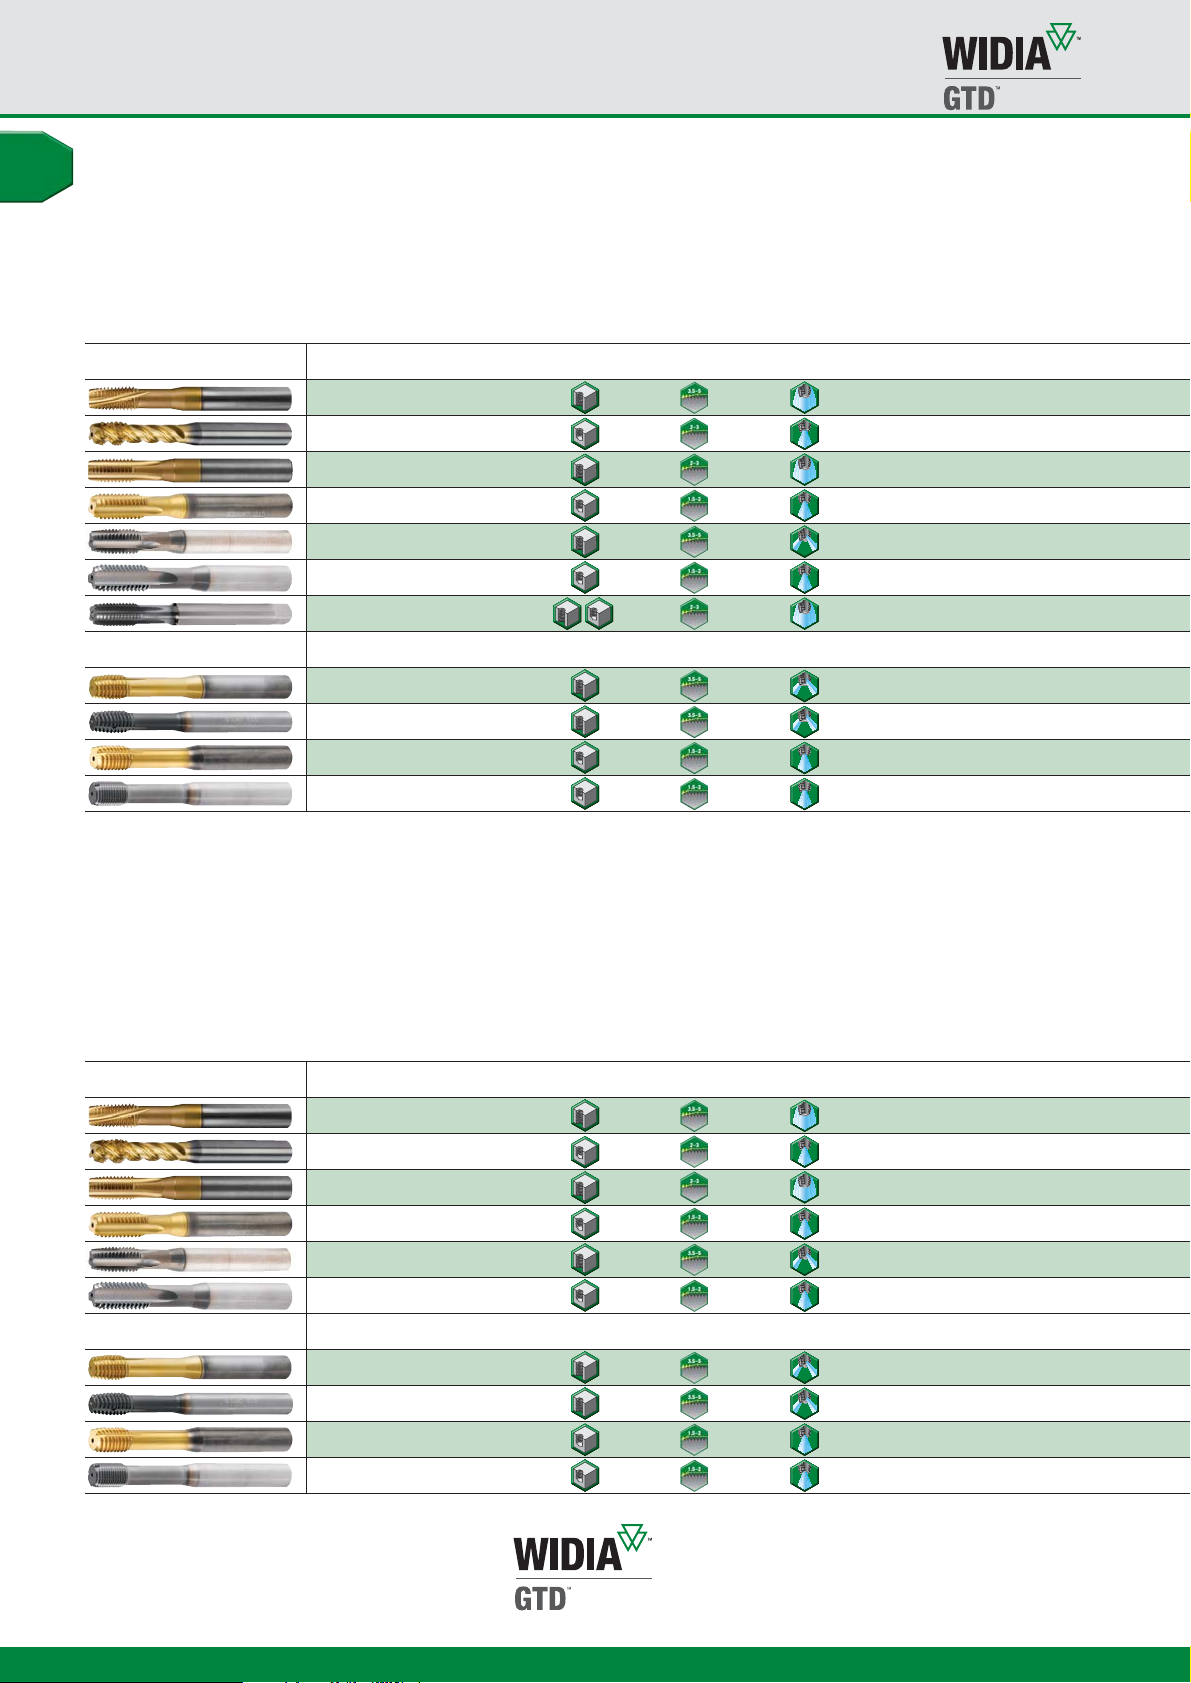
Taps Selection Guide • Solid Carbide Taps
Victory™GX Series HP Solid Carbide Taps and Solid Carbide Forming Taps • Metric
Good
多
Better
多多
Best
多多多
GX Series High-Performance
Solid Carbide Taps
series
GX32
size range
(inch and metric)
size
min - max
M6 - M16 GP4535 6535 HA
hole
chamfer
form
coolant grade shank
M6 - M16 GP4535 6535 HA
M4 - M20 GP4535 6535 HA
M4 - M16 GP4535 6535 HA
M6 - M16 GN1515 6535 HA
M6 - M16 GN1515 6535 HA
M3 - M16 WH16PG DIN371,374,376
M4 - M10 GP4535 6535 HA
M4 - M12 GN1515 6535 HA
M4 - M10 GP4535 6535 HA
M4 - M12 GN1515 6535 HA
Holemaking • High-Performance Taps
GX Series High-Performance
Solid Carbide Forming Taps
GX33
GX34
GX35
GX46
GX47
GX10
GX38
GX48
GX39
GX49
Victory GX Series HP Solid Carbide Taps and Solid Carbide Forming Taps • Inch
Good
多
Better
多多
Best
多多多
GX Series High-Performance
Solid Carbide Taps
series
GX32
size range
(inch and metric)
size
min - max
1/4" - 5/8" GP4535 6535 HA
hole
chamfer
form
coolant grade shank
GX Series High-Performance
Solid Carbide Forming Taps
A8
GX33
GX34
GX35
GX46
GX47
GX38
GX48
GX39
GX49
1/4" - 5/8" GP4535 6535 HA
#6 - 3/4" GP4535 6535 HA
#6 - 3/4" GP4535 6535 HA
1/4" - 5/8" GN1515 6535 HA
1/4" - 5/8" GN1515 6535 HA
#6 - 3/8" GP4535 6535 HA
#6 - 1/2" GN1515 6535 HA
#6 - 3/8" GP4535 6535 HA
#6 - 1/2" GN1515 6535 HA
WWW.WIDIA.COM
Page 8
High-Performance Taps
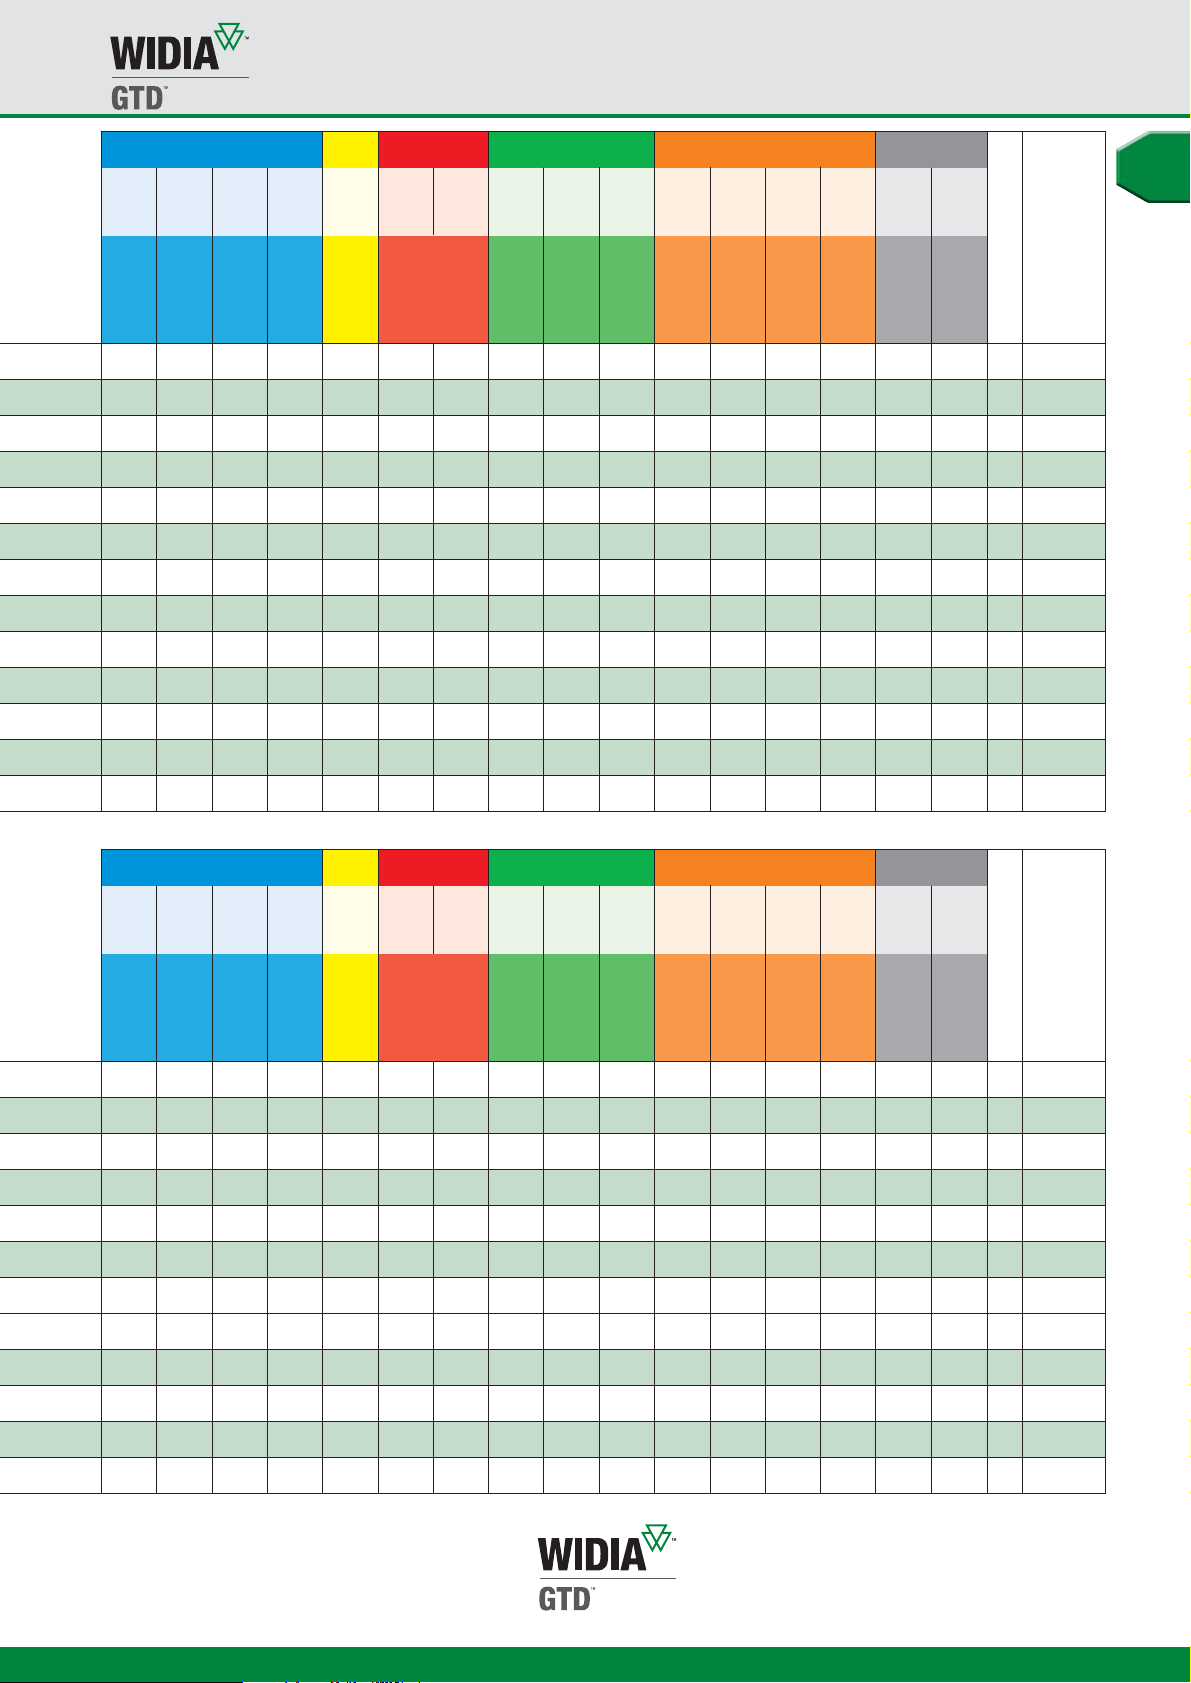
Taps Selection Guide • Solid Carbide Taps
P M K N S H
1, 2, 3,
4, 6, 7
<35 HRC
Steel
5, 9,
10, 11
Steel
36–48
HRC
12, 13.1 13.2
PH &
Steel
PH &
Ferriitic
Stainless
Steel
>35 HRC
Ferriitic
Stainless
<35 HRC
14.1, 14.2,
14.3, 14.4
Stainless
Steel
15, 16,
17, 18, 19
Cast Iron
多多多 多 多
多多多 多 多
多多多 多多多
多多多 多多多
多多多
多多多
20 21
Wrought
Aluminum
多多多 多多
多多多 多多
22, 23,
24, 25
Cast
Aluminum
多多多
多多多
26, 27,
28
Copper,
Copper
Alloys
31, 32
Iron
Based
33, 34,
35
Cobalt
Based
36 37
Nickel
Based
Titanium
& Alloys
38.1, 38.2,
40.1, 40.2,
41.1
Hardened
Steel
49–55
HRC
39.1,
41.2
Hardened
Steel
56–68
HRC
多多多
Recommended
Page
Cutting
Parameters
A12 A23
A13 A23
A14 A23
A15 A23
A18 A23
A19 A23
A22 A23
A16 A23
A20 A23
A17 A23
A21 A23
Holemaking • High-Performance Taps
P M K N S H
1, 2, 3,
4, 6, 7
<35 HRC
Steel
5, 9,
10, 11
Steel
36–48
HRC
12, 13.1 13.2
PH &
Steel
PH &
Ferriitic
Stainless
Steel
>35 HRC
Ferriitic
Stainless
<35 HRC
14.1, 14.2,
14.3, 14.4
Stainless
Steel
15, 16,
17, 18, 19
Cast Iron
多多多 多 多
多多多 多 多
多多多 多多多
多多多 多多多
多多多
多多多
20 21
Wrought
Aluminum
多多多 多多
多多多 多多
22, 23,
24, 25
Cast
Aluminum
多多多
多多多
26, 27,
28
Copper,
Copper
Alloys
31, 32
Iron
Based
33, 34,
35
Cobalt
Based
36 37
Nickel
Based
Titanium
& Alloys
38.1, 38.2,
40.1, 40.2,
41.1
Hardened
Steel
49–55
HRC
39.1,
41.2
Hardened
Steel
56–68
HRC
Recommended
Page
Cutting
Parameters
A12 A23
A13 A23
A14 A23
A15 A23
A18 A23
A19 A23
A16 A23
A20 A23
A17 A23
A21 A23
WWW.WIDIA.COM
A9
Page 9
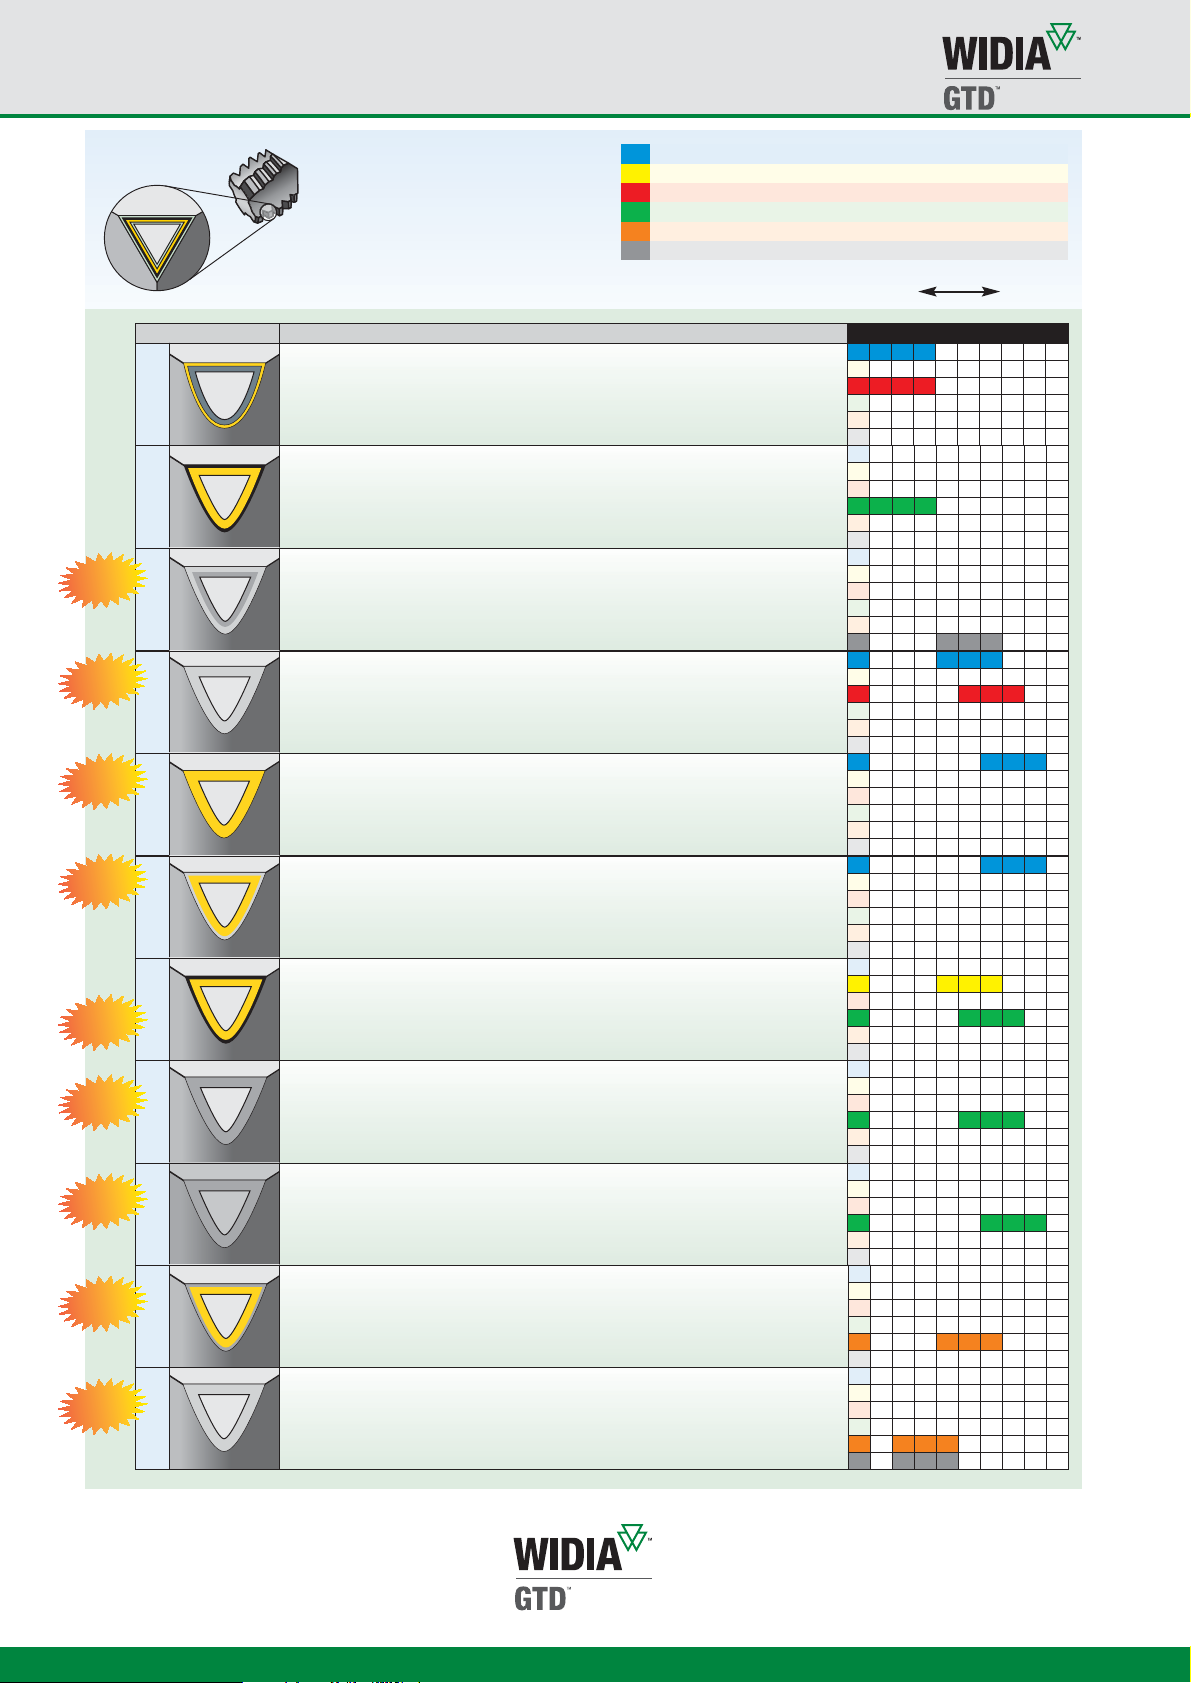
High-Performance Taps
Grades and Grade Descriptions
NEW!
NEW!
Coating
GP4535
GN1515
WH16PG
GP6520
Coatings are designed for
optimized tapping performance
in specific materials.
P Steel
M Stainless Steel
K Cast Iron
N Non-Ferrous Materials
S High-Temp Alloys
H Hardened Materials
Grade Description
Coated carbide, PVD multilayer coating with TiAlN and TiN over a high-strength carbide substrate
specifically designed for tap application. Use in steel up to 32 HRC and cast iron at four times faster
speeds than HSS-E-PM taps.
Coated carbide, PVD two-layer coating over fine-grain carbide. Coating consists of low-friction CrC/C over
wear-resistant TiN. CrC/C resists galling of non-ferrous materials to the tap. Provides superior perfomance
for tapping cast aluminum and other non-ferrous materials.
Coated carbide, PVD two-layer coating with heat-resistant TiAlN base layer and low-friction MoS2top layer
over carbide substrate. Use in hardened steel 55–63 HRC.
Coated HSS-E-PM, PVD heat- and wear-resistant high-vanadium cobalt powder metal HSS substrate
coated with wear-resistant TiCN base layer. Use in steel, cast iron, and cast aluminum with silicon.
wear
resistance toughness
05 10 15 20 25 30 35 40 45
P
K
N
H
P
K
NEW!
NEW!
NEW!
NEW!
NEW!
NEW!
Grade
WP31MG
WH36MG
GM6515
WN38MG
WN48EG
WN35MG
Coated HSS-E-PM, PVD powder metal HSS-E substrate with TiN coating. Use for tapping steel 32–44 HRC
and for forming threads in steel to 32 HRC.
Coated HSS-E-PM, PVD powder metal HSS-E substrate coated with TiN base layer and low-friction MoS
top layer. Use in deep blind steel holes, 32–44 HRC.
Coated HSS-E-PM, PVD heat- and wear-resistant high-vanadium cobalt powder metal HSS substrate.
Coating consists of low-friction CrC/C over wear-resistant TiN base layer. Use for tapping stainless steel
and non-ferrous materials.
Coated HSS-E-PM, PVD powder metal HSS-E substrate with DLC coating. Use for form tapping aluminum.
Not recommended for steel.
Coated HSS-E, PVD lower vanadium HSS-E substrate with DLC coating. Use for tapping non-ferrous
materials with low cutting temperatures like wrought aluminum. Not recommended for steel.
Coated HSS-E-PM, PVD powder metal HSS-E substrate with two-layer coating. TiN base layer and DLC top
layer that resists galling of non-ferrous materials to the tap. Use for tapping titanium. Not recommended
for steel.
P
P
2
M
N
N
N
S
NEW!
A10
WS32MG
Coated HSS-E-PM, PVD heat- and wear-resistant high-vanadium cobalt powder metal HSS substrate with
high-hardness TiCN coating. Use when tapping heat-treated steel 44–55 HRC and cobalt- or nickel-based
heat-resistant alloys.
S
H
WWW.WIDIA.COM
Page 10
Victory™GX HP Solid Carbide for the
Ultimate High-Performance Tapping Line
Run up to 4x faster and last up to 4x longer than conventional high-speed steel taps.
• Enhanced precision design delivers more accurately tapped holes.
• A full range of styles and grades for blind hole and through hole applications
in ferrous and non-ferrous materials.
• After use, cutting taps can be factory reconditioned to original patented
specifications and tolerances.
Machining Medium Carbon Steel
250
200
150
100
vc m/min
50
0
Turning Milling Drilling Tapping
To learn more about our innovations, contact your local Authorized Distributor
or visit www.widia.com.
New Victory GX Series Taps
HSS-E Taps
Page 11
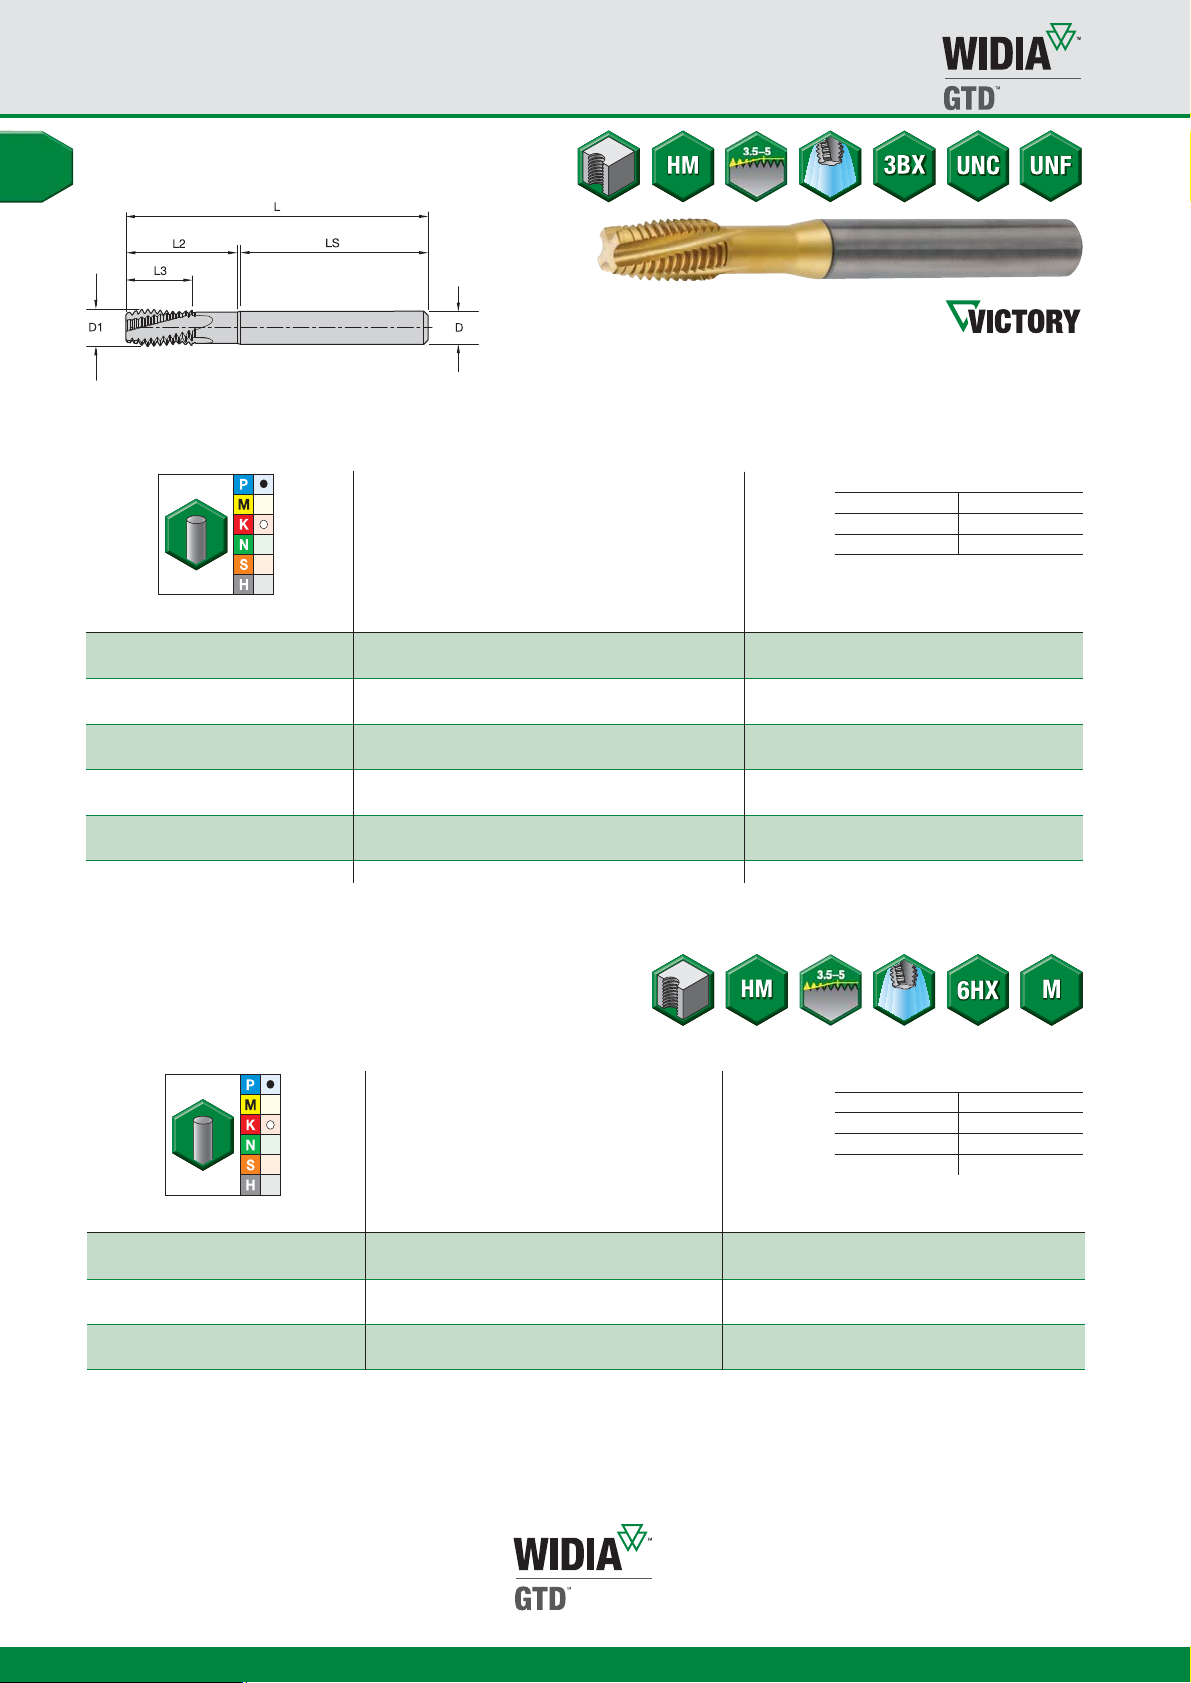
High-Performance Taps
Victory™Solid Carbide Left-Hand Spiral-Flute Taps • Through Holes
• GP4535 TiAlN + TiN for steel.
GX32 • Form D Plug Chamfer • Inch
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
GP4535 D1 size L
12200 1/4 - 20 2.76 .59 .91 1.67 .2500 3 3BX
12201 1/4 - 28 2.76 .59 .91 1.67 .2500 3 3BX
12202 5/16 - 18 3.15 .67 1.10 1.85 .3125 3 3BX
12203 5/16 - 24 3.15 .67 1.10 1.85 .3125 3 3BX
12204 3/8 - 16 3.54 .75 1.30 2.01 .3750 4 3BX
12205 3/8 - 24 3.54 .75 1.30 2.01 .3750 4 3BX
12206 7/16 - 14 3.94 .87 1.42 2.26 .4375 4 3BX
12207 1/2 - 13 3.94 .94 1.58 2.08 .5000 4 3BX
12208 1/2 - 20 3.94 .94 1.58 2.08 .5000 4 3BX
12209 9/16 - 12 4.33 1.02 1.85 2.35 .5000 4 3BX
12210 5/8 - 11 4.33 1.10 2.09 2.09 .5625 5 3BX
GX32 • Form D Plug Chamfer • Metric
L3 L2 LS D
number
of flutes
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
GP4535 D1 size L L3 L2 LS D
12225 M6 X 1 70 12 23 43 6,0 3 6HX
12226 M8 X 1,25 80 15 28 47 8,0 3 6HX
12227 M10 X 1,5 90 18 33 51 10,0 4 6HX
12228 M12 X 1,75 100 21 40 54 12,0 4 6HX
12229 M14 X 2 110 24 47 61 12,0 4 6HX
12230 M16 X 2 110 24 53 55 14,0 4 6HX
Proprietary technology.
A12
number
of flutes
class
of fit
WWW.WIDIA.COM
Page 12
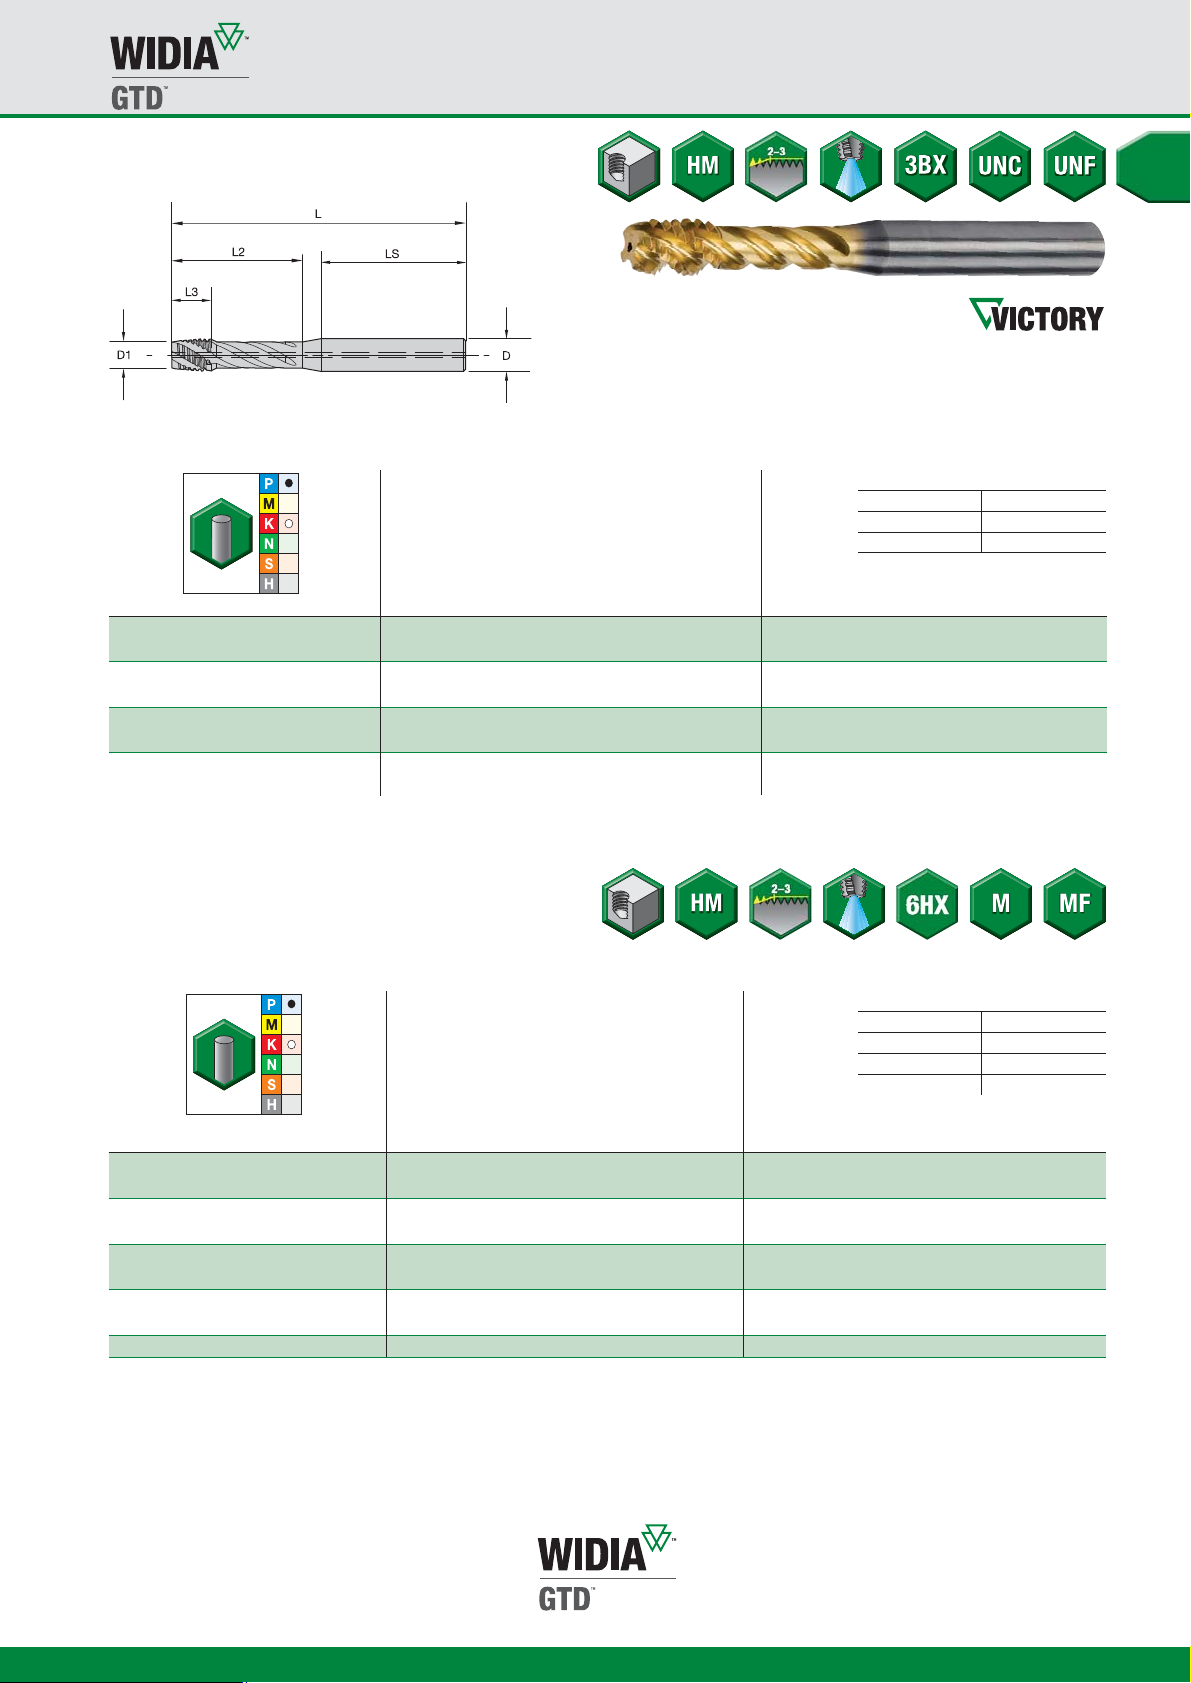
Victory™Solid Carbide Spiral-Flute Taps • Blind Holes
• GP4535 TiAlN + TiN for steel.
GX33 • Form C Semi-Bottoming Chamfer • Through Coolant • Inch
GP4535 D1 size L L3 L2 LS D
12761 1/4 - 20 2.76 .39 .94 1.63 .2500 3 3BX
12762 1/4 - 28 2.76 .39 .94 1.63 .2500 3 3BX
12763 5/16 - 18 3.15 .47 1.26 1.69 .3125 3 3BX
12764 3/8 - 16 3.54 .51 1.57 1.74 .3750 4 3BX
12765 7/16 - 14 3.94 .59 1.73 1.94 .4375 4 3BX
12766 1/2 - 13 3.94 .63 1.89 1.76 .5000 4 3BX
12767 9/16 - 12 4.33 .67 2.20 2.00 .5000 4 3BX
12768 5/8 - 11 4.33 .75 2.52 1.66 .5625 4 3BX
䢇
first choice
嘷
alternate choice
High-Performance Taps
Shank Tolerance
D Tolerance h6
0.250–0.375 +0, -0.0004
0.438–0.625 +0, -0.0004
number
of flutes
class
of fit
Holemaking • High-Performance Taps
GX33 • Form C Semi-Bottoming Chamfer • Through Coolant • Metric
GP4535 D1 size L L3 L2 LS D
12781 M6 X 1 70 8 24 42 6,0 3 6HX
12782 M8 X 1,25 80 10 32 43 8,0 3 6HX
12783 M10 X 1,5 90 12 40 44 10,0 4 6HX
12784 M10 X 1 90 12 40 44 10,0 4 6HX
12786 M12 X 1,5 100 14 48 46 12,0 4 6HX
12785 M12 X 1,75 100 14 48 46 12,0 4 6HX
12788 M14 X 1,5 110 16 56 52 12,0 4 6HX
12787 M14 X 2 110 16 56 52 12,0 4 6HX
12789 M16 X 2 110 16 64 44 14,0 4 6HX
Proprietary technology.
number
of flutes
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
WWW.WIDIA.COM
A13
Page 13
High-Performance Taps
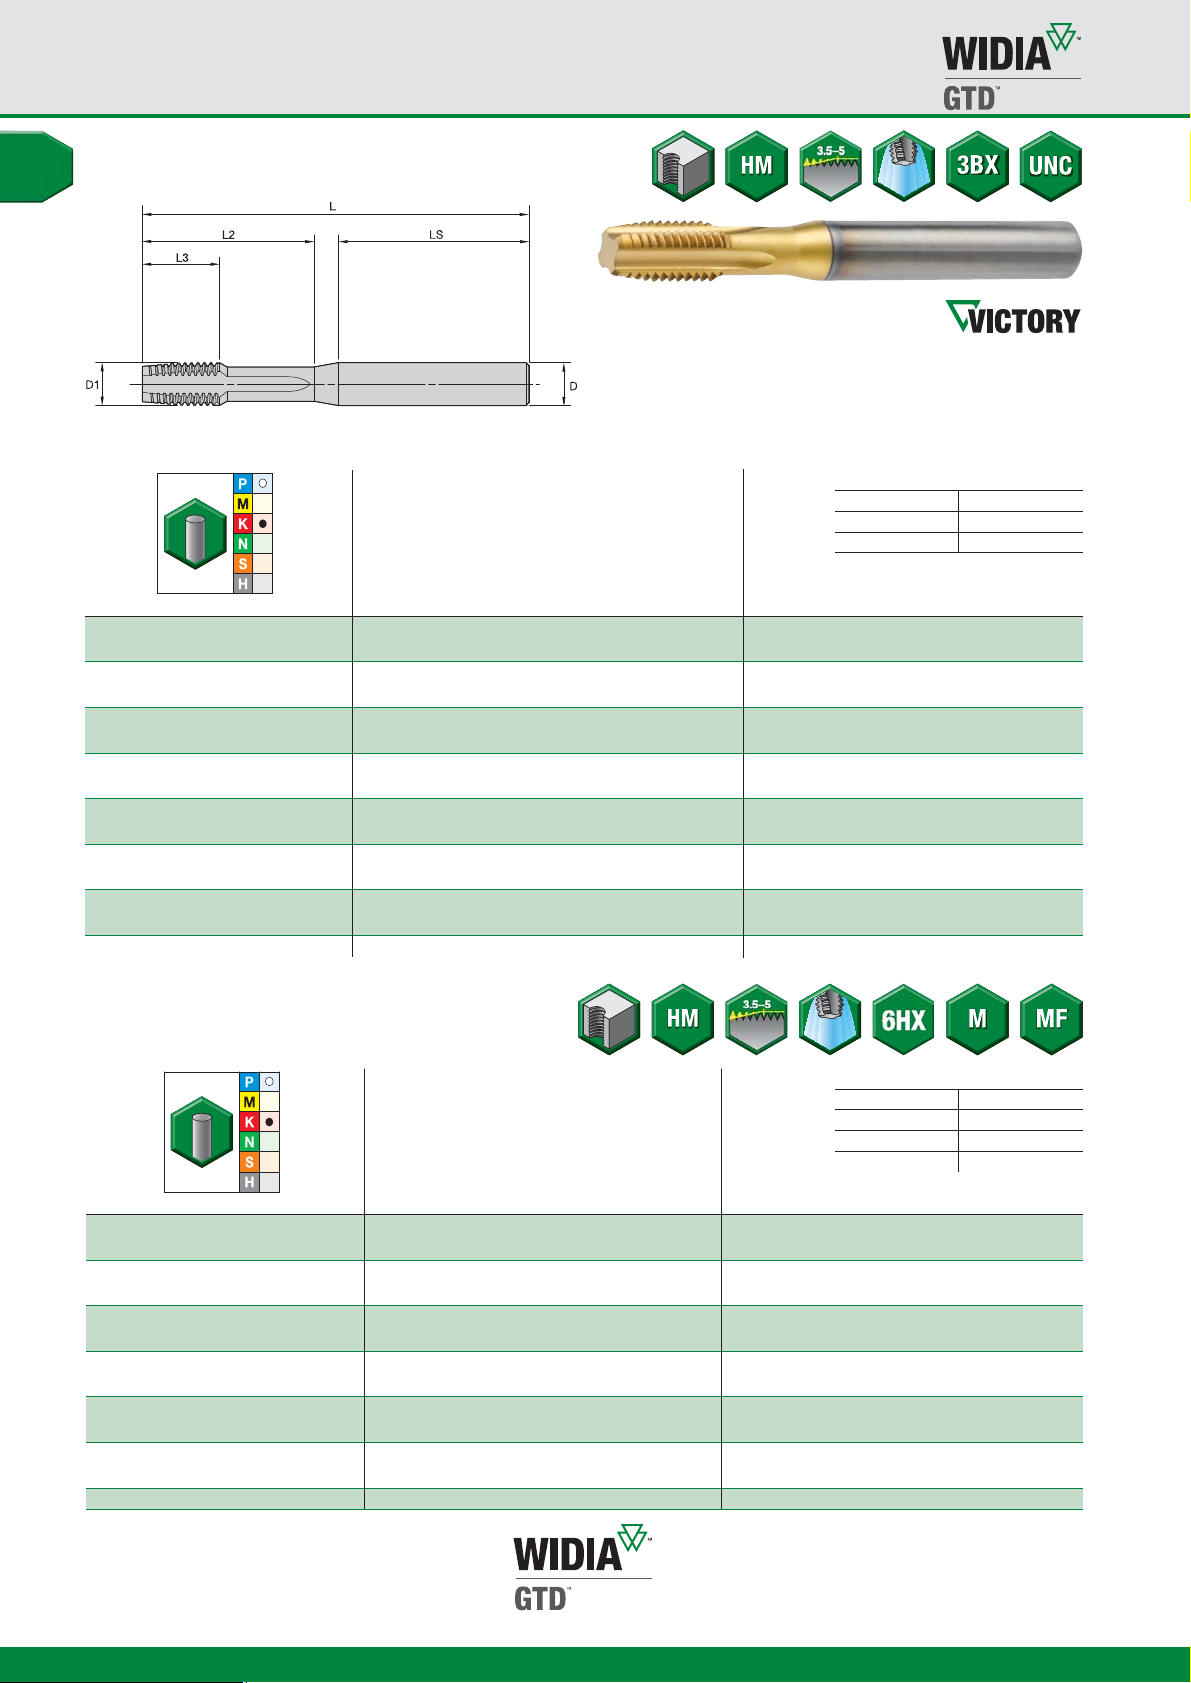
Victory™Solid Carbide Straight-Flute Taps • Through Holes
• GP4535 TiAlN + TiN for cast iron.
GX34 • Form D Plug Chamfer • Inch
Holemaking • High-Performance Taps
GP4535 D1 size L L3 L2 LS D
12713 6 - 32 2.36 .28 .55 1.37 .2500 3 3BX
12714 8 - 32 2.36 .28 .63 1.37 .2500 3 3BX
12715 10 - 24 2.36 .35 .79 1.25 .2500 3 3BX
12716 10 - 32 2.36 .35 .79 1.25 .2500 3 3BX
12717 1/4 - 20 2.76 .59 .91 1.67 .2500 4 3BX
12718 1/4 - 28 2.76 .59 .91 1.67 .2500 4 3BX
12719 5/16 - 18 3.15 .67 1.10 1.85 .3125 4 3BX
12404 3/8 - 16 3.54 .75 1.30 2.01 .3750 4 3BX
12405 3/8 - 24 3.54 .75 1.30 2.01 .3750 4 3BX
12406 7/16 - 14 3.94 .87 1.42 2.26 .4375 4 3BX
12407 1/2 - 13 3.94 .94 1.58 2.08 .5000 4 3BX
12408 1/2 - 20 3.94 .94 1.58 2.08 .5000 4 3BX
12409 9/16 - 12 4.33 1.02 1.85 2.35 .5000 4 3BX
12410 5/8 - 11 4.33 1.10 2.09 2.09 .5625 5 3B
12411 3/4 - 10 4.92 1.22 2.48 2.42 .6250 5 3BX
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
0.250–0.375 +0, -0.0004
0.438–0.625 +0, -0.0004
number
of flutes
class
of fit
GX34 • Form D Plug Chamfer • Metric
GP4535 D1 size L L3 L2 LS D
12742 M4 X 0,7 60 6 16 36 6,0 3 6HX
12743 M5 X 0,8 60 7 20 34 6,0 3 6HX
12744 M6 X 1 70 12 23 43 6,0 4 6HX
12745 M8 X 1,25 80 15 28 47 8,0 4 6HX
12427 M10 X 1,5 90 18 33 51 10,0 4 6HX
12746 M10 X 1 90 18 33 51 10,0 4 6HX
12747 M12 X 1,5 100 21 40 54 12,0 4 6HX
12428 M12 X 1,75 100 21 40 54 12,0 4 6HX
12429 M14 X 2 110 24 47 61 12,0 4 6HX
12748 M14 X 1,5 110 24 47 61 12,0 4 6HX
12430 M16 X 2 110 24 53 55 14,0 4 6HX
12431 M18 X 2,5 125 30 59 62 16,0 5 6HX
12432 M20 X 2,5 140 30 66 — 18,0 5 6HX
Proprietary technology.
A14
number
of flutes
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
WWW.WIDIA.COM
Page 14
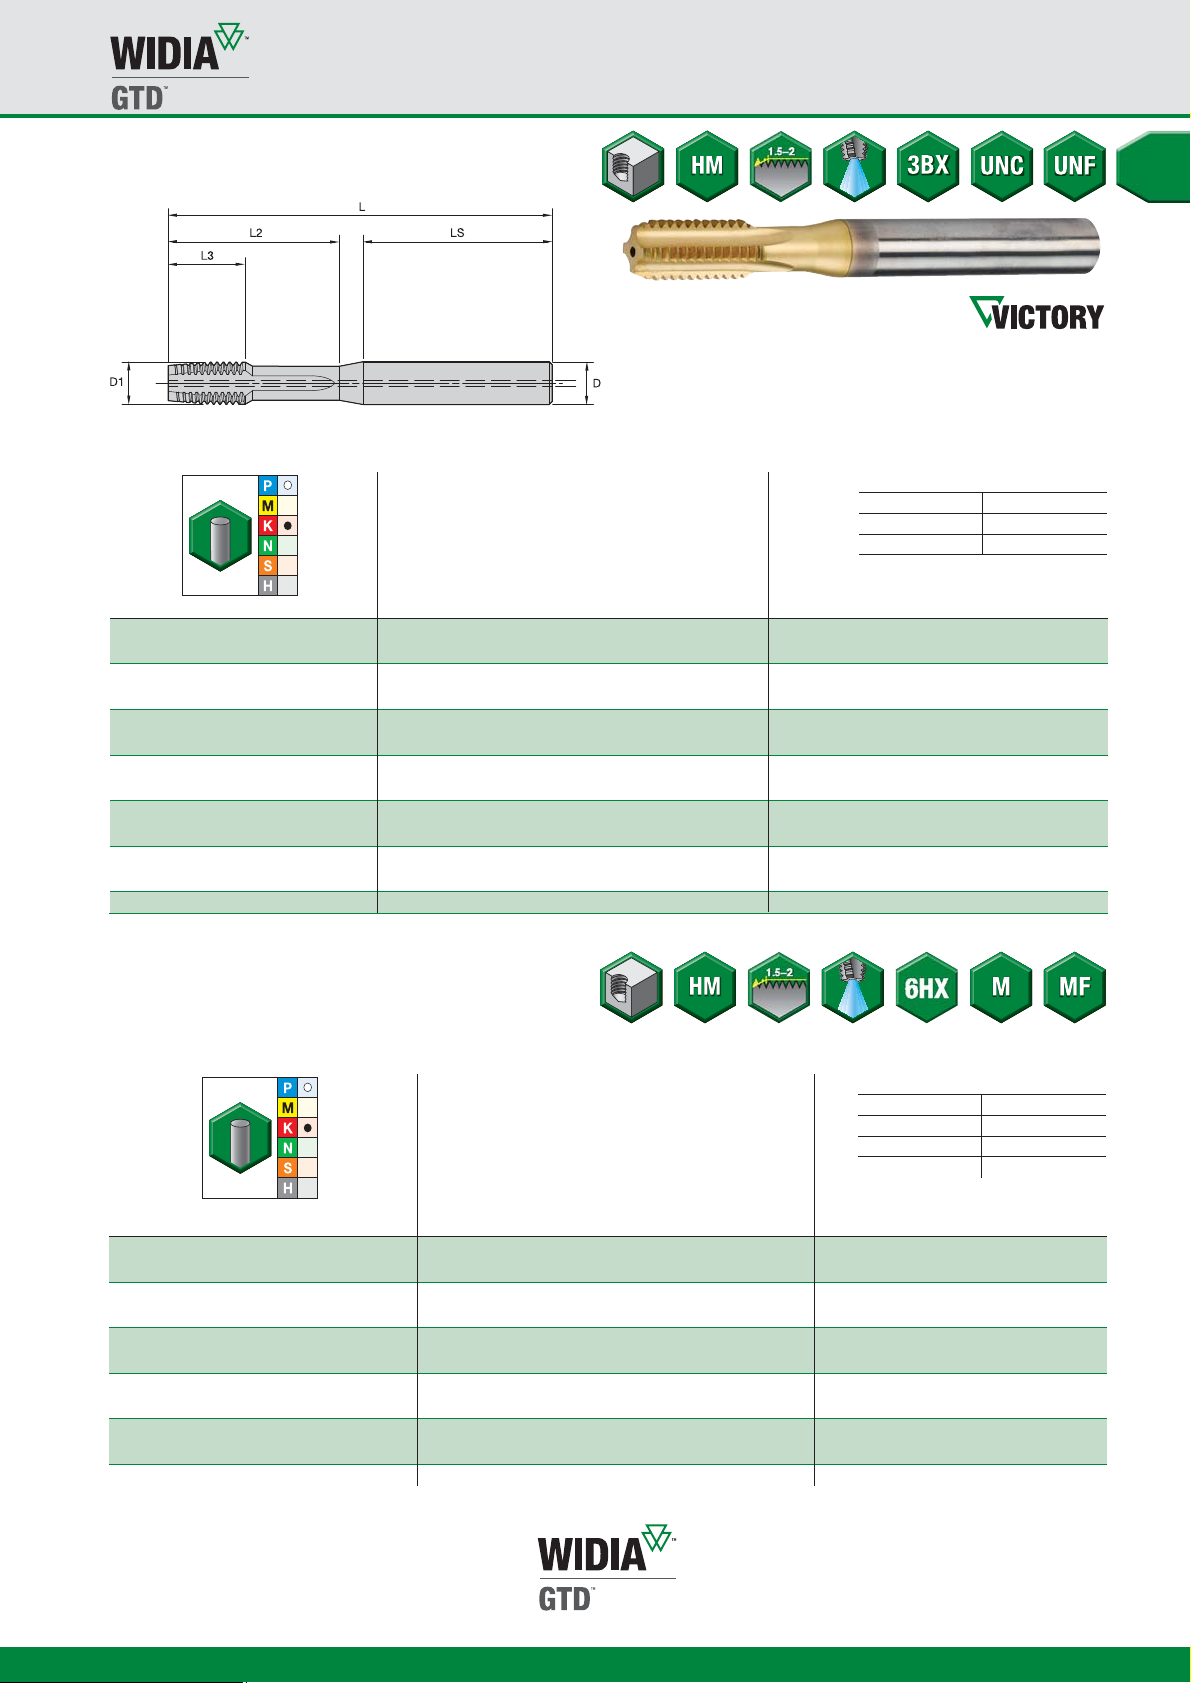
Victory™Solid Carbide Straight-Flute Taps • Blind Holes
• GP4535 TiAlN + TiN for tapping cast iron.
䢇
first choice
嘷
alternate choice
GX35 • Form E Bottoming Chamfer • Through Coolant 1/4" and Larger • Inch
GP4535 D1 size L L3 L2 LS D
12700 6 - 32 2.36 .28 .55 1.37 .2500 3 3BX
12701 8 - 32 2.36 .28 .63 1.37 .2500 3 3BX
12702 10 - 24 2.36 .35 .79 1.25 .2500 3 3BX
12703 10 - 32 2.36 .35 .79 1.25 .2500 3 3BX
12704 1/4 - 20 2.76 .59 .91 1.67 .2500 4 3BX
12705 1/4 - 28 2.76 .59 .91 1.67 .2500 4 3BX
12706 5/16 - 18 3.15 .67 1.10 1.85 .3125 4 3BX
12707 3/8 - 16 3.54 .75 1.30 2.01 .3750 4 3BX
12708 7/16 - 14 3.94 .87 1.42 2.26 .4375 4 3BX
12709 1/2 - 13 3.94 .94 1.57 2.08 .5000 4 3BX
12710 9/16 - 12 4.33 1.02 1.85 2.35 .5000 4 3BX
12711 5/8 - 11 4.33 1.10 2.09 2.09 .5625 5 3BX
12712 3/4 - 10 4.92 1.22 2.48 2.42 .6250 5 3BX
High-Performance Taps
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
number
of flutes
class
of fit
Holemaking • High-Performance Taps
GX35 • Form E Bottoming Chamfer • Through Coolant M6 and Larger • Metric
GP4535 D1 size L L3 L2 LS D
12731 M4 X 0,7 60 6 16 36 6,0 3 6HX
12732 M5 X 0,8 60 7 20 34 6,0 3 6HX
12733 M6 X 1 70 12 23 43 6,0 4 6HX
12734 M8 X 1,25 80 15 28 47 8,0 4 6HX
12736 M10 X 1 90 18 33 51 10,0 4 6HX
12735 M10 X 1,5 90 18 33 51 10,0 4 6HX
12738 M12 X 1,5 100 21 40 54 12,0 4 6HX
12737 M12 X 1,75 100 21 40 54 12,0 4 6HX
12740 M14 X 1,5 110 24 47 61 12,0 4 6HX
12739 M14 X 2 110 24 47 61 12,0 4 6HX
12741 M16 X 2 110 24 53 55 14,0 4 6HX
Proprietary technology.
WWW.WIDIA.COM
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
number
of flutes
class
of fit
A15
Page 15
High-Performance Taps
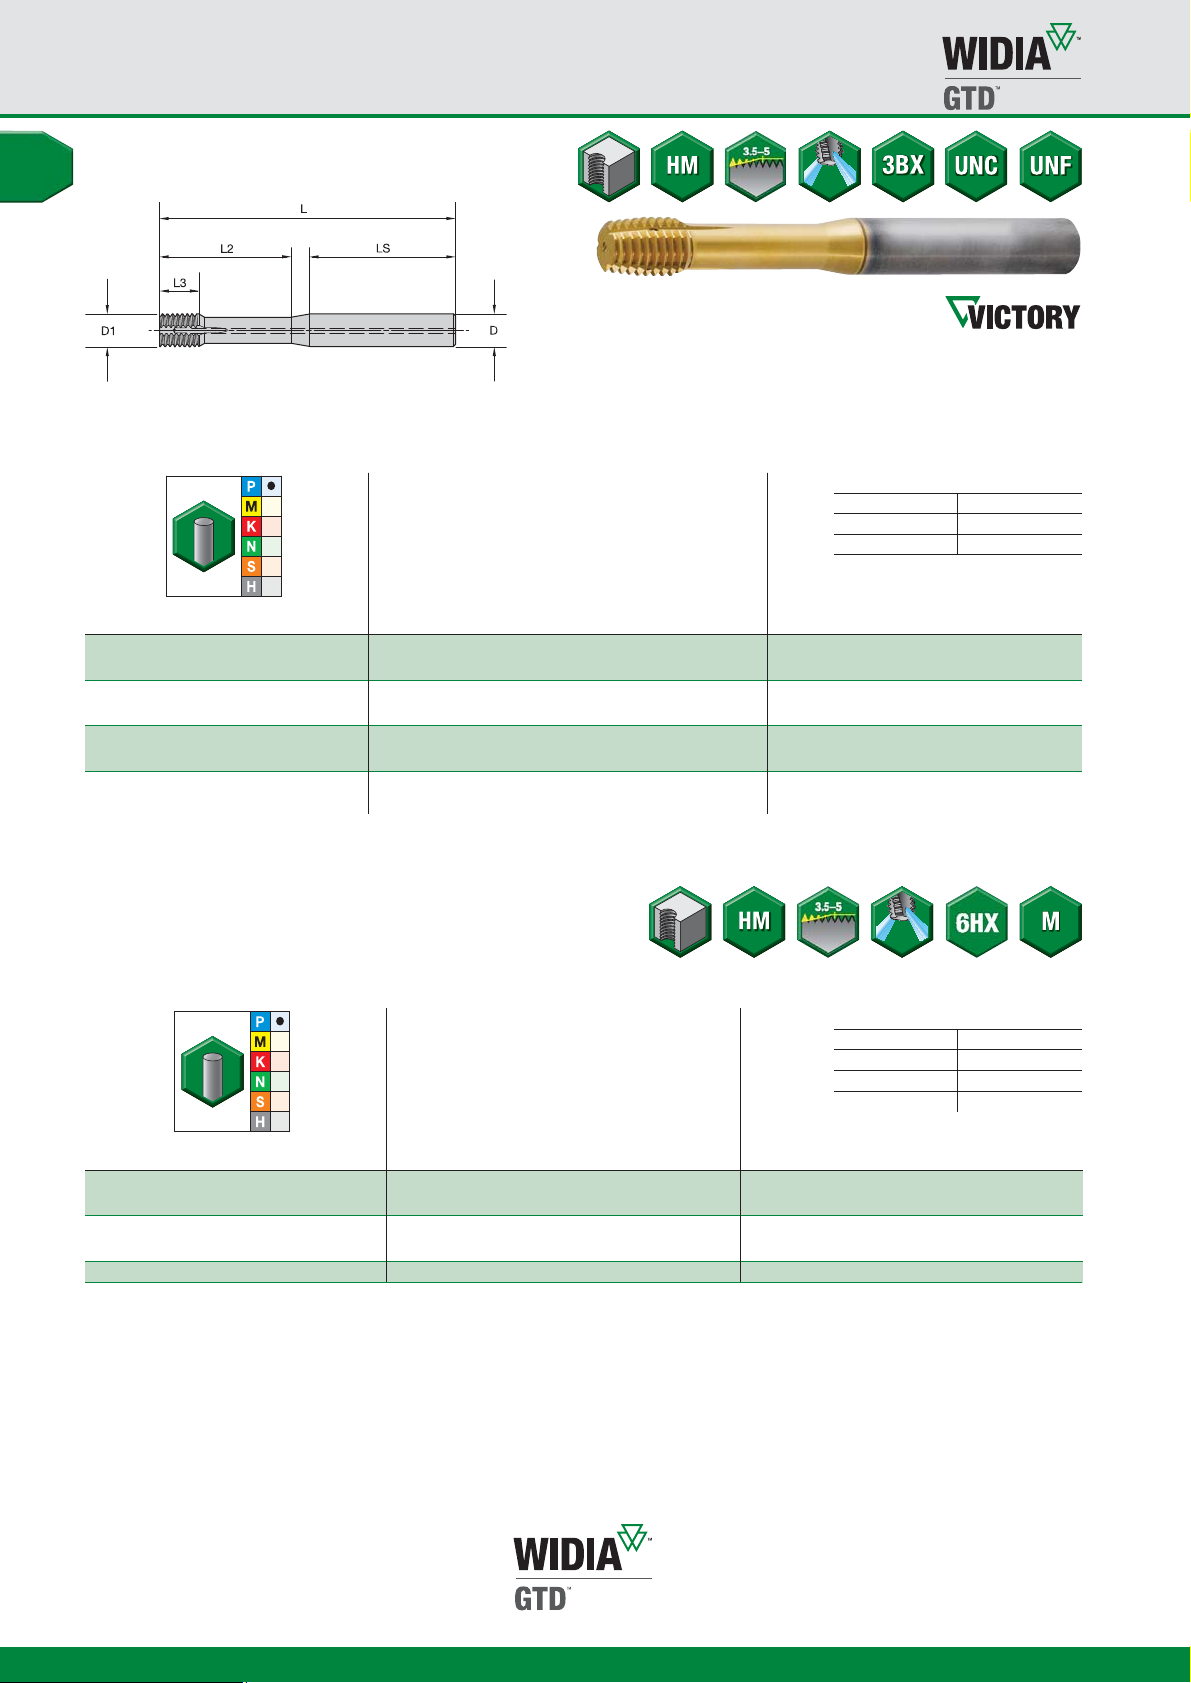
Victory™Solid Carbide Forming Taps • Through Holes
• GP4535 TiAlN + TiN for tapping steel.
GX38 • Form D Plug Entry Taper • Through Coolant 1/4" and Larger • Inch
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
GP4535
12809 6 - 32 2.36 .28 .55 1.37 .2500 2 3BX
12810 8 - 32 2.36 .28 .63 1.37 .2500 2 3BX
12811 10 - 24 2.36 .35 .79 1.25 .2500 2 3BX
12812 10 - 32 2.36 .35 .79 1.25 .2500 2 3BX
12813 1/4 - 20 2.76 .39 .95 1.63 .2500 2 3BX
12814 1/4 - 28 2.76 .39 .95 1.63 .2500 2 3BX
12815 5/16 - 18 3.15 .47 1.26 1.69 .3125 2 3BX
12816 3/8 - 16 3.54 .51 1.58 1.74 .3750 3 3BX
GX38 • Form D Plug Entry Taper • Coolant M6 and Larger • Metric
GP4535 D1 size L L3 L2 LS D
12831 M4 X 0,7 60 6 16 36 6,0 2 6HX
12832 M5 X 0,8 60 7 20 34 6,0 2 6HX
12833 M6 X 1 70 8 24 42 6,0 2 6HX
12834 M8 X 1,25 80 10 32 43 8,0 2 6HX
12835 M10 X 1,5 90 12 40 44 10,0 3 6HX
Proprietary technology.
Form taps require a larger drilled hole size prior to tapping than corresponding cutting taps.
D1 size
LL3L2 LS D
number of
lube grooves
number of
lube grooves
class
of fit
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
A16
WWW.WIDIA.COM
Page 16
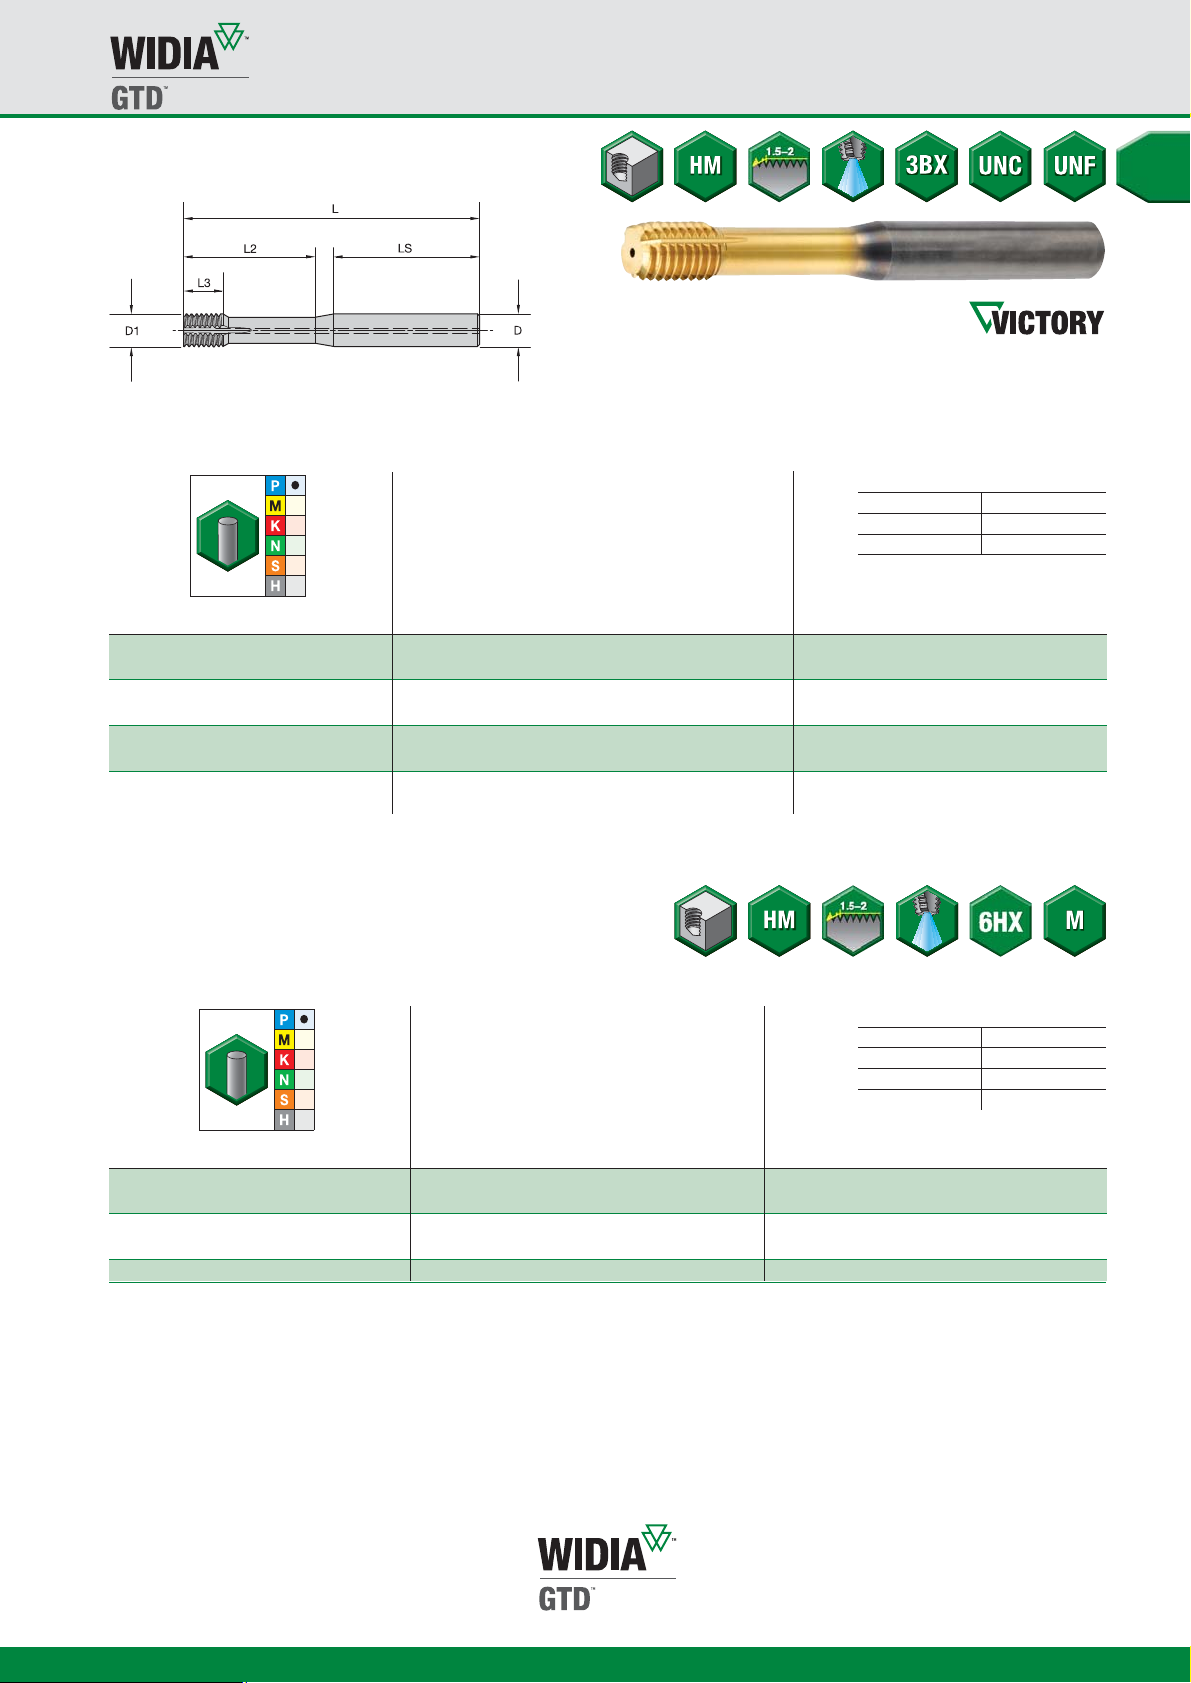
Victory™Solid Carbide Forming Taps • Blind Holes
• GP4535 TiAlN + TiN for tapping steel.
䢇
first choice
嘷
alternate choice
GX39 • Form E Bottoming Entry Taper • Through Coolant 1/4" and Larger • Inch
High-Performance Taps
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
Holemaking • High-Performance Taps
GP4535 D1 size L L3 L2 LS D
12801 6 - 32 2.36 .28 .55 1.37 .2500 2 3BX
12802 8 - 32 2.36 .28 .63 1.37 .2500 2 3BX
12803 10 - 24 2.36 .35 .79 1.25 .2500 2 3BX
12804 10 - 32 2.36 .35 .79 1.25 .2500 2 3BX
12805 1/4 - 20 2.76 .39 .95 1.63 .2500 2 3BX
12806 1/4 - 28 2.76 .39 .95 1.63 .2500 2 3BX
12807 5/16 - 18 3.15 .47 1.26 1.69 .3125 2 3BX
12808 3/8 - 16 3.54 .51 1.58 1.74 .3750 3 3BX
GX39 • Form E Bottoming Entry Taper • Through Coolant M6 and Larger • Metric
GP4535 D1 size L L3 L2 LS D
12826 M4 X 0,7 60 6 16 36 6,0 2 6HX
12827 M5 X 0,8 60 7 20 34 6,0 2 6HX
12828 M6 X 1 70 8 24 42 6,0 2 6HX
12829 M8 X 1,25 80 10 32 43 8,0 2 6HX
12830 M10 X 1,5 90 12 40 44 10,0 3 6HX
Proprietary technology.
Form taps require a larger drilled hole size prior to tapping than corresponding cutting taps.
number of
lube grooves
number of
lube grooves
class
of fit
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
WWW.WIDIA.COM
A17
Page 17
High-Performance Taps
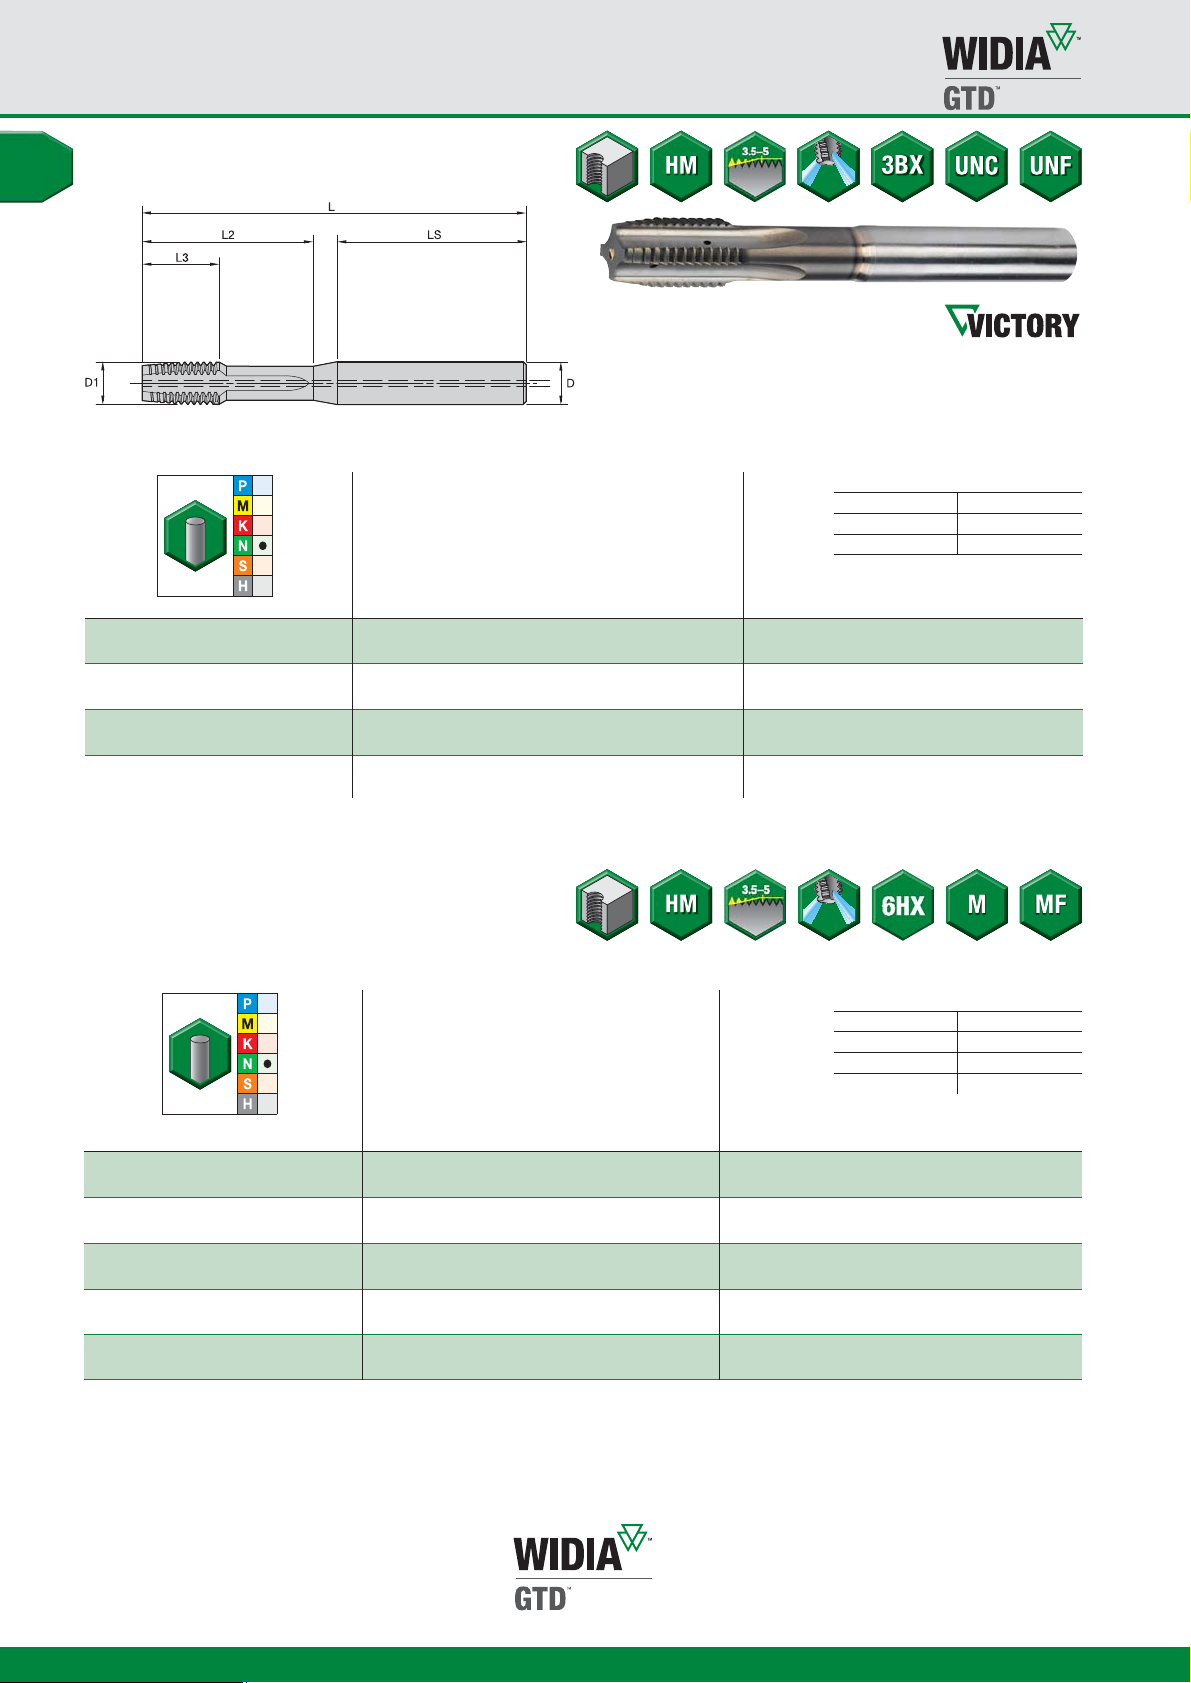
Victory™Solid Carbide Straight-Flute Taps • Through Holes
• GN1515 TiN + CrC/C for aluminum.
GX46 • Form D Plug Chamfer • Through Coolant 1/4" and Larger • Inch
Holemaking • High-Performance Taps
GN1515 D1 size L L3 L2 LS D
12836 1/4 - 20 2.76 .59 .94 1.63 .2500 3 3BX
12838 1/4 - 28 2.76 .59 .94 1.63 .2500 3 3BX
12839 5/16 - 18 3.15 .67 1.26 1.69 .3125 3 3BX
12840 3/8 - 16 3.54 .75 1.57 1.74 .3750 3 3BX
12841 7/16 - 14 3.94 .87 1.73 1.94 .4375 3 3BX
12843 1/2 - 13 3.94 .94 1.89 1.76 .5000 3 3BX
12844 9/16 - 12 4.33 1.02 2.20 2.00 .5000 4 3BX
12845 5/8 - 11 4.33 1.10 2.52 1.66 .5625 4 3BX
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
number
of flutes
class
of fit
GX46 • Form D Plug Chamfer • Through Coolant M6 and Larger • Metric
GN1515 D1 size L L3 L2 LS D
12846 M6 X 1 70 12 24 42 6,0 3 6HX
12847 M8 X 1,25 80 15 32 43 8,0 3 6HX
12848 M10 X 1,5 90 18 40 44 10,0 3 6HX
12850 M10 X 1 90 18 40 44 10,0 3 6HX
12852 M12 X 1,5 100 21 48 46 12,0 3 6HX
12851 M12 X 1,75 100 21 48 46 12,0 3 6HX
12854 M14 X 1,5 110 24 56 52 12,0 4 6HX
12853 M14 X 2 110 24 56 52 12,0 4 6HX
12856 M16 X 1,5 110 24 64 44 14,0 4 6HX
12855 M16 X 2 110 24 64 44 14,0 4 6HX
Proprietary technology.
number
of flutes
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
A18
WWW.WIDIA.COM
Page 18
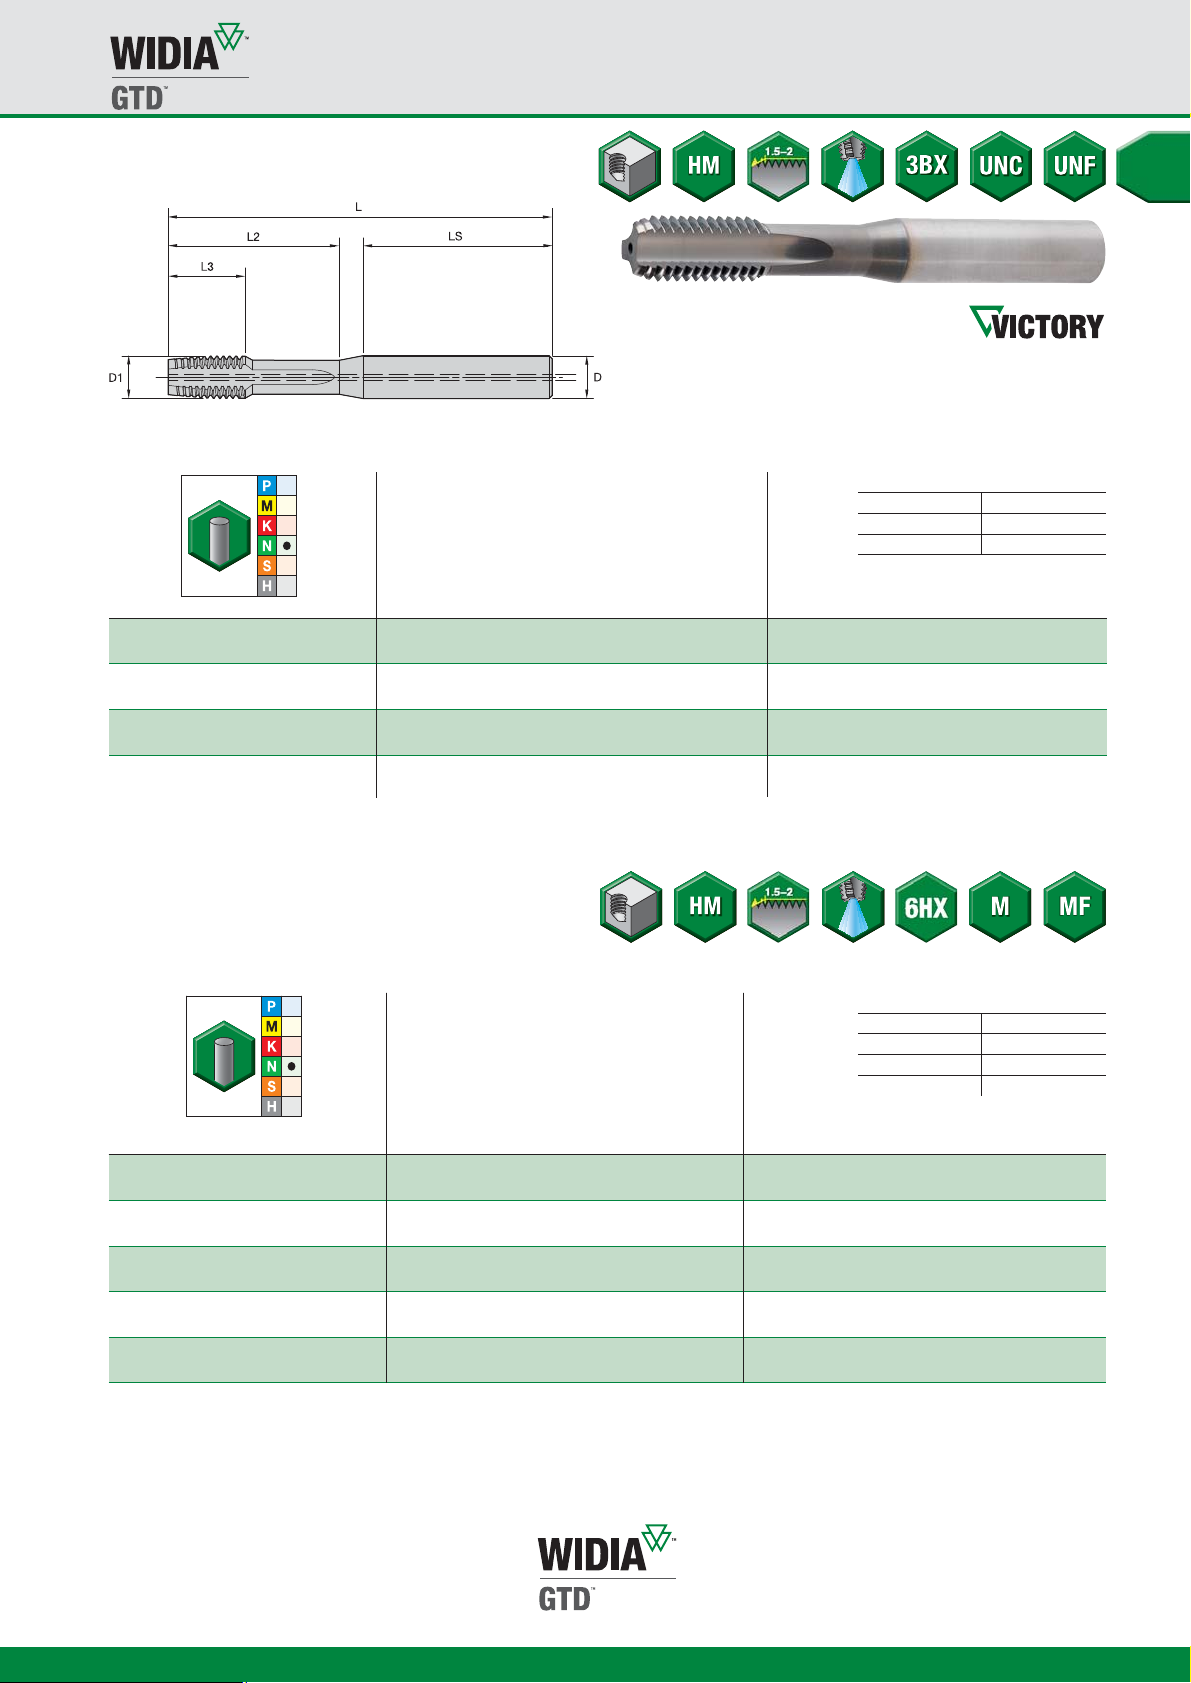
• GN1515 TiN + CrC/C for aluminum.
GX47 • Form E Bottoming Chamfer • Through Coolant • Inch
GN1515 D1 size L L3 L2 LS D
12858 1/4 - 20 2.76 .59 .94 1.63 .2500 3 3BX
12859 1/4 - 28 2.76 .59 .94 1.63 .2500 3 3BX
12860 5/16 - 18 3.15 .67 1.26 1.69 .3125 3 3BX
12861 3/8 - 16 3.54 .75 1.57 1.74 .3750 3 3BX
12862 7/16 - 14 3.94 .87 1.73 1.94 .4375 3 3BX
12863 1/2 - 13 3.94 .94 1.89 1.76 .5000 3 3BX
12864 9/16 - 12 4.33 1.02 2.20 2.00 .5000 4 3BX
12865 5/8 - 11 4.33 1.10 2.52 1.66 .5625 4 3BX
High-Performance Taps
Victory™Solid Carbide Straight-Flute Taps • Blind Holes
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
number
of flutes
class
of fit
Holemaking • High-Performance Taps
GX47 • Form E Bottoming Chamfer • Through Coolant • Metric
GN1515 D1 size L L3 L2 LS D
12866 M6 X 1 70 12 24 42 6,0 3 6HX
12867 M8 X 1,25 80 15 32 43 8,0 3 6HX
12868 M10 X 1,5 90 18 40 44 10,0 3 6HX
12869 M10 X 1 90 18 40 44 10,0 3 6HX
12872 M12 X 1,5 100 21 48 46 12,0 3 6HX
12870 M12 X 1,75 100 21 48 46 12,0 3 6HX
12874 M14 X 1,5 110 24 56 52 12,0 4 6HX
12873 M14 X 2 110 24 56 52 12,0 4 6HX
12876 M16 X 1,5 110 24 64 44 14,0 4 6HX
12875 M16 X 2 110 24 64 44 14,0 4 6HX
Proprietary technology.
number
of flutes
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
WWW.WIDIA.COM
A19
Page 19
High-Performance Taps
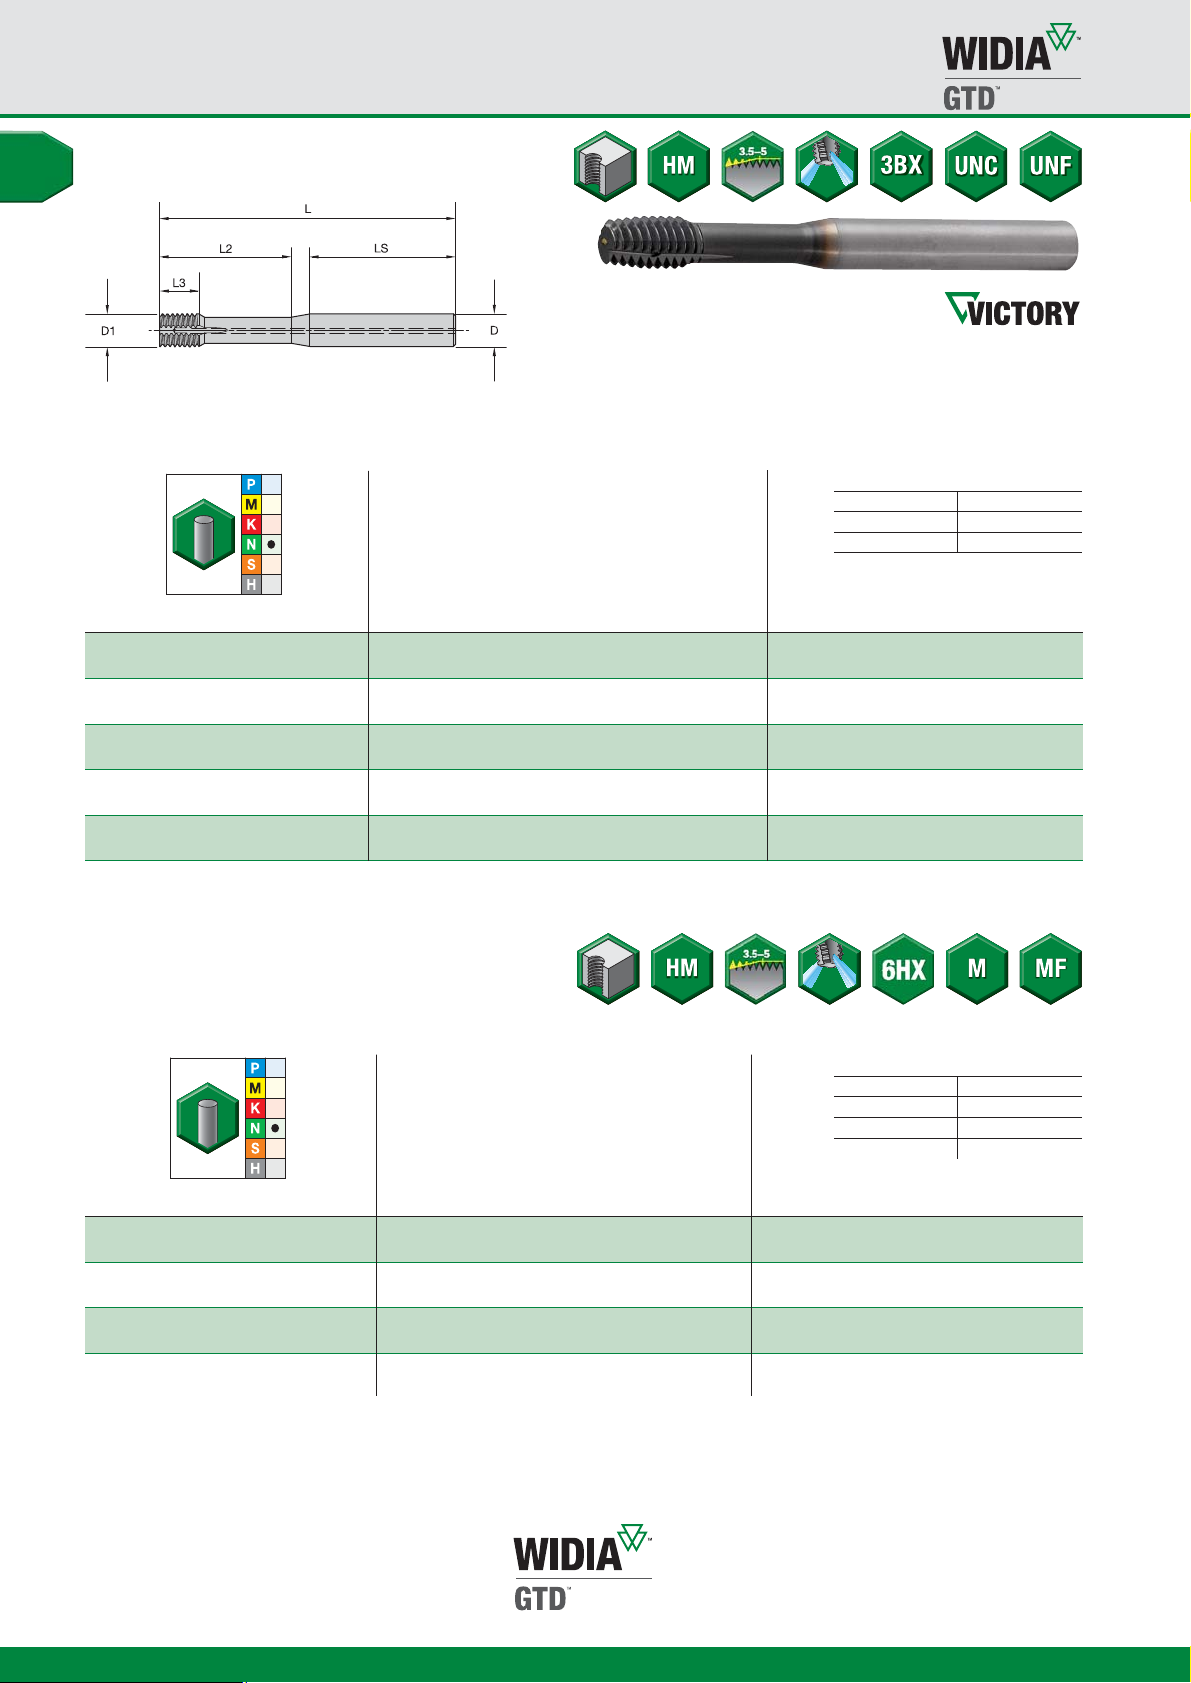
Victory™Solid Carbide Forming Taps • Through Holes
• GN1515 TiN + CrC/C for aluminum.
GX48 • Form D Plug Entry Taper • Through Coolant 1/4" and Larger • Inch
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
GN1515 D1 size L L3 L2 LS D
12877 6 - 32 2.36 .28 .55 1.37 .2500 2 3BX
12878 8 - 32 2.36 .28 .63 1.37 .2500 2 3BX
12879 10 - 24 2.36 .35 .79 1.25 .2500 2 3BX
12880 10 - 32 2.36 .35 .79 1.25 .2500 2 3BX
12881 1/4 - 20 2.76 .39 .94 1.63 .2500 2 3BX
12882 1/4 - 28 2.76 .39 .94 1.63 .2500 2 3BX
12883 5/16 - 18 3.15 .47 1.26 1.69 .3125 2 3BX
12884 3/8 - 16 3.54 .51 1.57 1.74 .3750 3 3BX
12885 7/16 - 14 3.94 .59 1.73 1.94 .4375 3 3BX
12886 1/2 - 13 3.94 .63 1.89 1.76 .5000 3 3BX
GX48 • Form D Plug Entry Taper • Coolant M6 and Larger • Metric
number of
lube grooves
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
Shank Tolerance
D Tolerance h6
6 +0, -0,008
GN1515 D1 size L L3 L2 LS D
12887 M4 X 0,7 60 6 16 36 6,0 2 6HX
12888 M5 X 0,8 60 7 20 34 6,0 2 6HX
12889 M6 X 1 70 8 24 42 6,0 2 6HX
12890 M8 X 1,25 80 10 32 43 8,0 2 6HX
12891 M10 X 1,5 90 12 40 44 10,0 3 6HX
12892 M10 X 1 90 12 40 44 10,0 3 6HX
12894 M12 X 1,5 100 14 48 46 12,0 3 6HX
12893 M12 X 1,75 100 14 48 46 12,0 3 6HX
Proprietary technology.
Form taps require a larger drilled hole size prior to tapping than corresponding cutting taps.
A20
number of
lube grooves
class
of fit
WWW.WIDIA.COM
Page 20
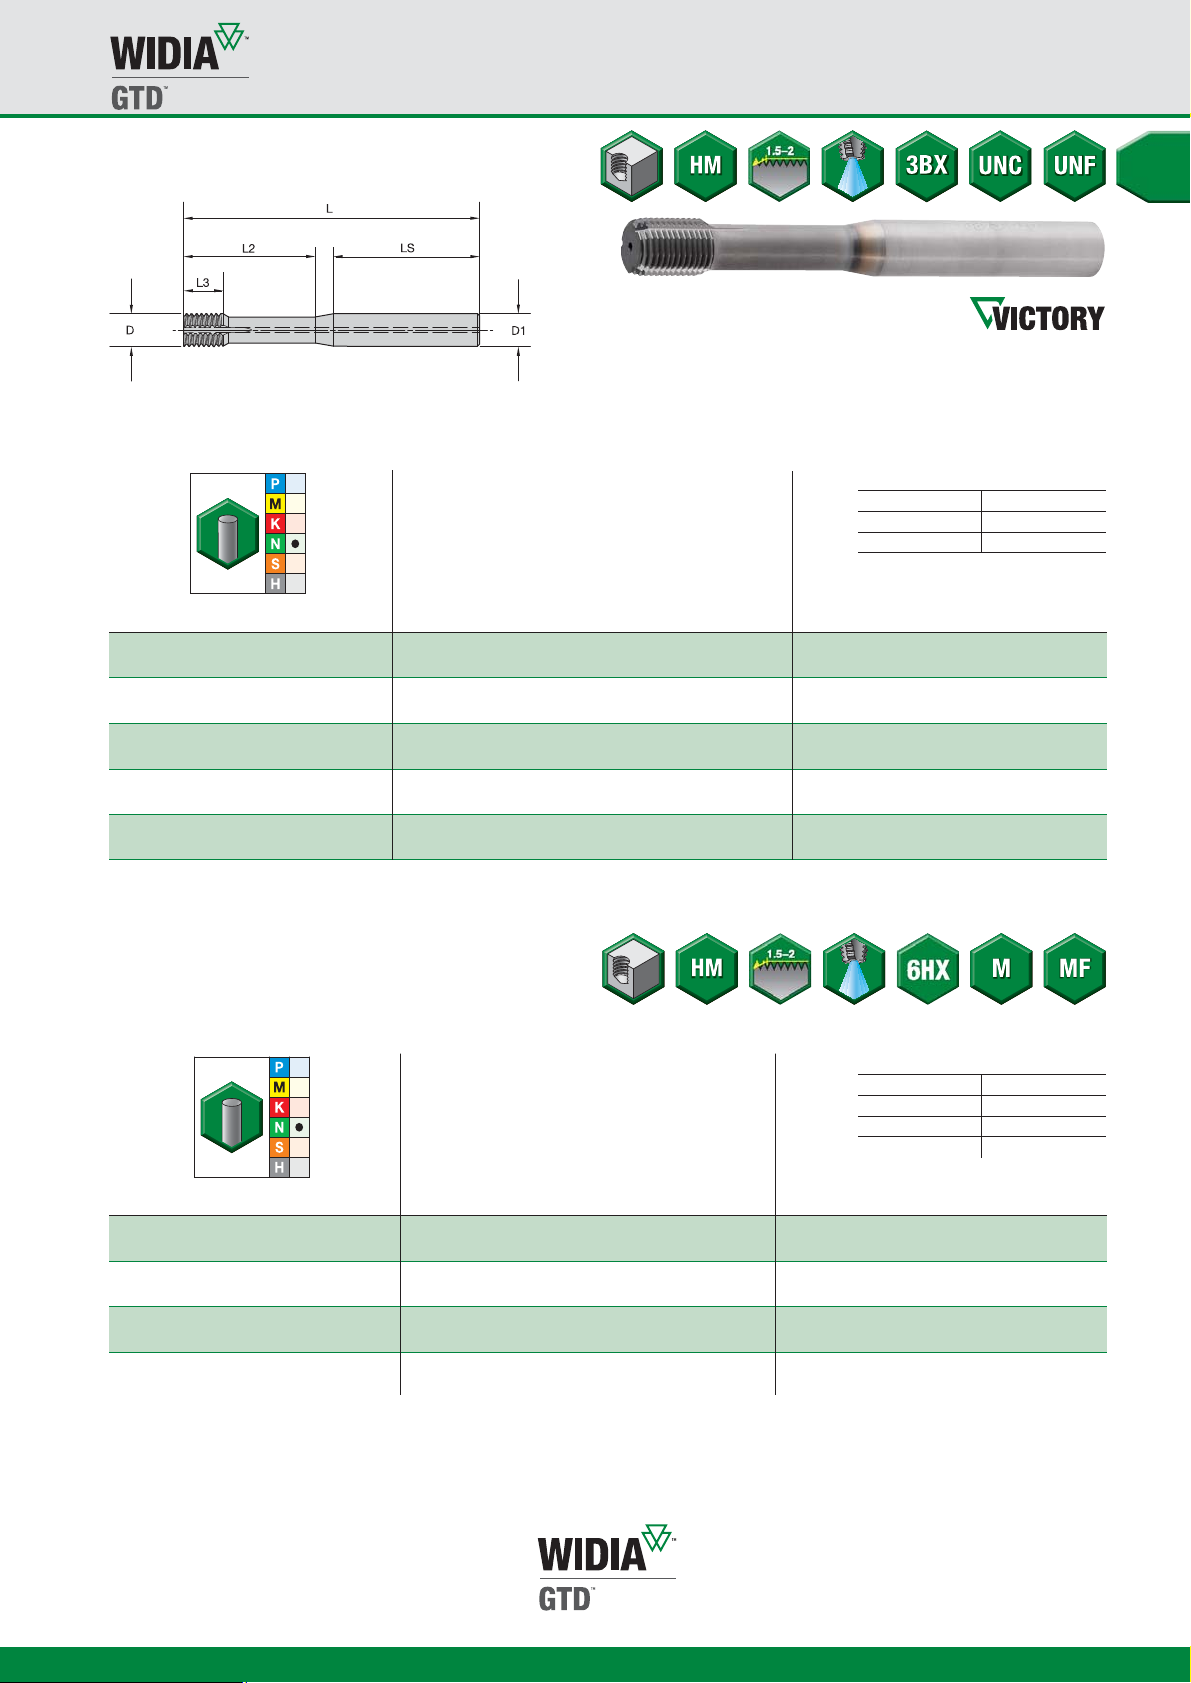
Victory™Solid Carbide Forming Taps • Blind Holes
• GN1515 TiN + CrC/C for aluminum.
䢇
first choice
嘷
alternate choice
GX49 • Form E Bottoming Entry Taper • Through Coolant 1/4" and Larger • Inch
High-Performance Taps
Shank Tolerance
D Tolerance h6
.250–.375 +0, -.0004
.438–.625 +0, -.0004
Holemaking • High-Performance Taps
GN1515 D1 size L L3 L2 LS D
12895 6 - 32 2.36 .28 .55 1.37 .2500 2 3BX
12896 8 - 32 2.36 .28 .63 1.37 .2500 2 3BX
12897 10 - 24 2.36 .35 .79 1.25 .2500 2 3BX
12898 10 - 32 2.36 .35 .79 1.25 .2500 2 3BX
12899 1/4 - 20 2.76 .39 .94 1.63 .2500 2 3BX
12901 1/4 - 28 2.76 .39 .94 1.63 .2500 2 3BX
12902 5/16 - 18 3.15 .47 1.26 1.69 .3125 2 3BX
12903 3/8 - 16 3.54 .51 1.57 1.74 .3750 3 3BX
12904 7/16 - 14 3.94 .59 1.73 1.94 .4375 3 3BX
12905 1/2 - 13 3.94 .63 1.89 1.76 .5000 3 3BX
GX49 • Form E Bottoming Entry Taper • Through Coolant M6 and Larger • Metric
number of
lube grooves
class
of fit
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
GN1515 D1 size L L3 L2 LS D
12906 M4 X 0,7 60 6 16 36 6,0 2 6HX
12907 M5 X 0,8 60 7 20 34 6,0 2 6HX
12908 M6 X 1 70 8 24 42 6,0 2 6HX
12909 M8 X 1,25 80 10 32 43 8,0 2 6HX
12911 M10 X 1,5 90 12 40 44 10,0 3 6HX
12912 M10 X 1 90 12 40 44 10,0 3 6HX
12915 M12 X 1,5 100 14 48 46 12,0 3 6HX
12914 M12 X 1,75 100 14 48 46 12,0 3 6HX
Proprietary technology.
Form taps require a larger drilled hole size prior to tapping than corresponding cutting taps.
WWW.WIDIA.COM
number of
lube grooves
class
of fit
A21
Page 21
High-Performance Taps
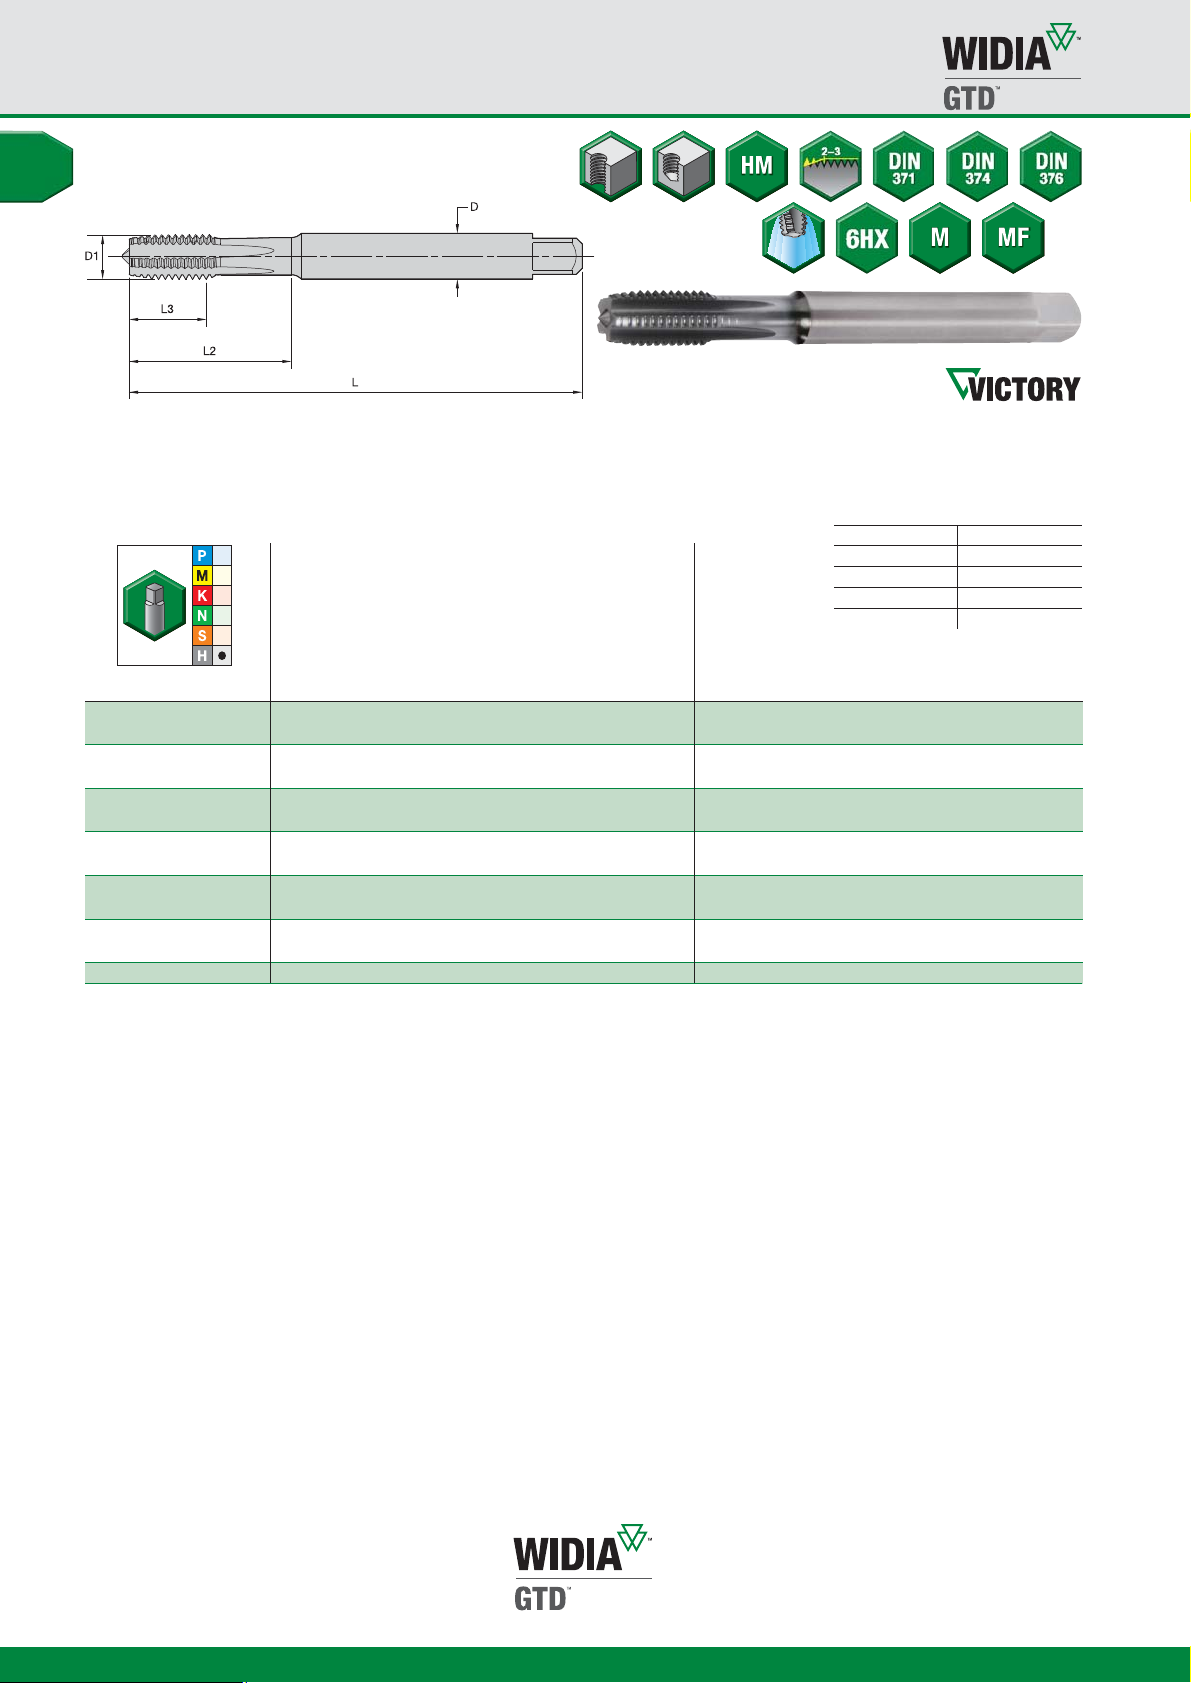
Victory™Straight-Flute Carbide Taps • Blind and Through Holes
• WH16PG TiAlN/MoS
GX10 • Form C Semi-Bottoming Chamfer • Metric DIN 371, 374, and 376
Holemaking • High-Performance Taps
WH16PG D1 size L L3 L2 D
GX105001 M3 X 0,5 63 6 18 4,5 4 DIN 371 6HX
GX105002 M4 X 0,7 63 8 20 4,5 4 DIN 371 6HX
GX105003 M5 X 0,8 70 10 26 6,0 4 DIN 371 6HX
GX105004 M6 X 1 80 12 28 6,0 4 DIN 371 6HX
GX105009 M8 X 1 90 15 35 8,0 5 DIN 374 6HX
GX105005 M8 X 1,25 90 15 35 8,0 5 DIN 371 6HX
GX105010 M10 X 1 100 18 38 10,0 5 DIN 374 6HX
GX105006 M10 X 1,5 100 18 38 10,0 5 DIN 371 6HX
GX105011 M12 X 1,5 110 21 41 12,0 5 DIN 374 6HX
GX105007 M12 X 1,75 110 21 41 12,0 5 DIN 376 6HX
GX105012 M14 X 1,5 110 24 44 14,0 5 DIN 374 6HX
GX105008 M14 X 2 110 24 44 14,0 6 DIN 376 6HX
GX105013 M16 X 1,5 110 24 44 16,0 5 DIN 374 6HX
for steel 55–63 HRC.
2
䢇
first choice
嘷
alternate choice
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
A22
WWW.WIDIA.COM
Page 22
Through Holes Blind Holes
Group Tap Style Grade min
1 GX32, GX38 GP4535 80
P
2 GX32, GX38 GP4535 70
3, 4, 6, 7 GX32, GX38 GP4535 60
15, 16 GX34 GP4535 80
K
17, 18, 19 GX34 GP4535 80
20 GX34 GP4535 70
21 GX46, GX48 GN1515 90
N
22, 23, 24 GX46, GX48 GN1515 80
25 GX46, GX48 GN1515 70
39.1, 41.2 GX10 WH16PG 1,2
H
39.1 GX10 WH16PG 0,6
High-Performance Taps
Application Data • Carbide
Range — m/min Range — m/min
Starting
Value max Tap Style Grade min
100
90
80
105
100
90
120
100
85
1,5
0,8
130 GX33,GX39 GP4535 50
120 GX33,GX39 GP4535 50
100 GX33,GX39 GP4535 50
140 GX35 GP4535 50
130 GX35 GP4535 50
120 GX35 GP4535 50
160 GX47, GX49 GN1515 60
130 GX47, GX49 GN1515 50
110 GX47, GX49 GN1515 50
2,0 GX10 WH16PG 0,8
1,0 GX10 WH16PG 0,4
Starting
Value max
70
60
60
70
70
60
80
70
60
1,1
0,5
90
80
80
90
90
80
100
90
80
1,4
0,7
Holemaking • High-Performance Taps
Through Holes Blind Holes
Group Tap Style Grade min
1 GX32, GX38 GP4535 260
P
2 GX32, GX38 GP4535 230
3, 4, 6, 7 GX32, GX38 GP4535 200
15, 16 GX34 GP4535 260
K
17, 18, 19 GX34 GP4535 260
20 GX34 GP4535 230
21 GX46, GX48 GN1515 300
N
22, 23, 24 GX46, GX48 GN1515 260
25 GX46, GX48 GN1515 230
39.1, 41.2 GX10 WH16PG 4
H
39.1 GX10 WH16PG 2
Range — SFM Range — SFM
Starting
Value max Tap Style Grade min
330
300
260
340
330
300
390
330
280
5
2
430 GX33, GX39 GP4535 160
390 GX33, GX39 GP4535 160
330 GX33, GX39 GP4535 160
460 GX34 GP4535 160
430 GX34 GP4535 160
390 GX34 GP4535 160
520 GX47, GX49 GN1515 200
430 GX47, GX49 GN1515 160
360 GX47, GX49 GN1515 160
6 GX10 WH16PG 3
3 GX10 WH16PG 1
Starting
Value max
230
200
200
230
230
200
260
230
200
3
2
300
260
260
300
300
260
330
300
260
4
2
WWW.WIDIA.COM
A23
Page 23
High-Performance Taps
Cross Reference Chart • Solid Carbide Taps and Drills
Steel
Solid Carbide Taps
P
Solid Carbide Taps
typical
thread sizes
cutting taps
metric inch metric inch mm inch fraction wire GX33_GP4535 GX32_GP4535 GX39_GP4535
— — — 6-32 3,175 .1250 1/8 — — — 12801
M4,5 x 0,75 — M4 x 0,70 — 3,700 .1457 — — — — 12826
— — — 8-32 3,797 .1495 — 25 — — 12802
— — — 10-24 4,366 .1719 11/64 — — — 12803
— 12-24 — 10-32 4,496 .1770 — 16 — — 12804
— — M5 x 0,80 — 4,700 .1850 — 13 — — 12827
M6 x 1,00 — — — 5,000 .1969 — — 12781 12225 —
— 1/4-20 — 12-28 5,106 .2010 — 7 12761 12200 —
— 1/4-28 — — 5,410 .2130 — 3 12762 12201 —
Holemaking • High-Performance Taps
— — M6 x 1,00 — 5,600 .2205 — — — — 12828
— — — 1/4-20 5,791 .2280 — 1 — — 12805
— — — 1/4-28 5,944 .2340 — A — — 12806
— 5/16-18 — — 6,528 .2570 — F 12763 12202 —
M8 x 1,25 — — — 6,700 .2638 — — 12782 12226 —
— 5/16-24 — — 6,909 .2720 — I — 12203 —
— — — 5/16-18 7,366 .2900 — L — — 12807
— — M8 x 1,25 — 7,400 .2913 — — — — 12829
— 3/8-16 — — 7,938 .3125 5/16 — 12764 12204 —
— 3/8-24 — — 8,433 .3320 — Q — 12205 —
M10 x 1,50 — — — 8,500 .3346 — — 12783 12227 —
M10 x 1,00 — — — 9,000 .3543 — — 12784 — —
— — — 3/8-16 8,839 .3480 — S — — 12808
— 7/16-14 — 3/8-24 9,093 .3580 — T 12765 12206 —
— — M10 x 1,50 — 9,400 .3701 — — — — 12830
M12 x 1,75 — — — 10,200 .4016 — — 12785 12228 —
M12 x 1,50 — — — 10,500 .4134 — — 12786 —
— 1/2-13 — — 10,716 .4219 27/64 — 12766 12207 —
— 1/2-20 — — 11,509 .4531 29/64 — — 12208 —
M14 x 2,00 — — — 12,000 .4724 — — 12787 12229 —
— 9/16-12 — — 12,304 .4844 31/64 — 12767 12209 —
M14 x 1,50 — — — 12,500 .4921 — — 12788 —
— 5/8-11 — 9/16-12 13,495 .5313 17/32 — 12768 12210 —
M16 x 2,00 — — — 14,000 .5512 — — 12789 12230 —
forming taps
required
tap drill diameter
blind hole forming blind hole
with coolant through hole with coolant
A24
WWW.WIDIA.COM
Page 24
High-Performance Taps
Cross Reference Chart • Solid Carbide Taps and Drills
P P
Solid Carbide Taps
forming through hole approximately 5 x D approximately 5 x D approximately 5 x D approximately 5 x D
with coolant with coolant non-coolant with coolant non-coolant
GX38_GP4535 TDS402 WP20PD TDS202 WP20PD VDS402A WU25PD VDS202A WU25PD
12809 TDS402A03175 TDS202A03175 VDS402A03175 VDS202A03175
12831 TDS402A03700 TDS202A03700 VDS402A03700 VDS202A03700
12810 TDS402A03797 TDS202A03797 VDS402A03797 VDS202A03797
12811 TDS402A04219 TDS202A04219 VDS402A04219 VDS202A04219
12812 TDS402A04496 TDS202A04496 VDS402A04496 VDS202A04496
12832 TDS402A04700 TDS202A04700 VDS402A04700 VDS202A04700
— TDS402A05000 TDS202A05000 VDS402A05000 VDS202A05000
— TDS402A05106 TDS202A05106 VDS402A05106 VDS202A05106
— TDS402A05410 TDS202A05410 VDS402A05410 VDS202A05410
12833 TDS402A05600 TDS202A05600 VDS402A05600 VDS202A05600
12813 TDS402A05791 TDS202A05791 VDS402A05791 VDS202A05791
12814 TDS402A05944 TDS202A05944 VDS402A05944 VDS202A05944
— TDS402A06528 TDS202A06528 VDS402A06528 VDS202A06528
— TDS402A06700 TDS202A06700 VDS412A06700 VDS212A06700
— TDS402A06906 TDS202A06906 VDS412A06906 VDS212A06906
12815 TDS402A07366 TDS202A07366 VDS412A07366 VDS212A07366
12834 TDS402A07400 TDS202A07400 VDS412A07400 VDS212A07400
— TDS402A07938 TDS202A07938 VDS412A07938 VDS212A07938
— TDS402A08433 TDS202A08433 VDS412A08433 VDS212A08433
— TDS402A08500 TDS202A08500 VDS412A08500 VDS212A08500
— TDS402A09000 TDS202A09000 VDS412A09000 VDS212A09000
12816 TDS402A08839 TDS202A08839 VDS412A08839 VDS212A08839
— TDS402A09093 TDS202A09093 VDS412A09093 VDS212A09093
12835 TDS402A09400 TDS202A09400 VDS412A09400 VDS212A09400
— TDS402A10200 TDS202A10200 VDS412A10200 VDS212A10200
— TDS402A10500 TDS202A10500 VDS412A10500 VDS212A10500
— TDS402A10716 TDS202A10716 VDS412A10716 VDS212A10716
— TDS402A11509 TDS202A11509 VDS412A11509 VDS212A11509
— TDS402A12000 TDS202A12000 VDS412A12000 VDS212A12000
— TDS402A12304 TDS202A12304 VDS412A12304 VDS212A12304
— TDS402A12500 TDS202A12500 VDS412A12500 VDS212A12500
— TDS402A13495 TDS202A13495 VDS412A13495 VDS212A13495
— TDS402A14000 TDS202A14000 VDS412A14000 VDS212A14000
Recommended SC Drill
All Materials
Alternate Tap Drill
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A25
Page 25
High-Performance Taps
Cross Reference Chart • Solid Carbide Taps and Drills
Cast Iron
Solid Carbide Taps
K
Recommended SC Drill
typical
thread sizes
cutting taps
metric inch mm inch fraction wire GX35_GP4535 GX34_GP4535 TDS411 WK15PD
— 6-32 2,705 .1065 — 36 12700 12713 TDS401A02705
M4 x 0,70 — 3,300 .1299 — — 12731 12742 TDS401A03300
— 8-32 /8-36 3,454 .1360 — 29 12701 12714 TDS401A03454
— 10-24 3,734 .1470 — 26 12702 12715 TDS401A03734
— 10-32 4,039 .1590 — 21 12703 12716 TDS401A04039
M5 x 0,80 — 4,200 .1654 — — 12732 12743 TDS401A04200
M6 x 1,00 — 5,000 .1969 — — 12733 12744 TDS401A05000
— 1/4-20 5,106 .2010 — 7 12704 12717 TDS401A05106
— 1/4-28 5,410 .2130 — 3 12705 12718 TDS401A05410
— 5/16-18 6,528 .2570 — F 12706 12719 TDS401A06528
M8 x 1,25 — 6,700 .2638 — — 12734 12745 TDS411A06700
Holemaking • High-Performance Taps
— 3/8-16 7,938 .3125 5/16 — 12707 12404 TDS411A07938
— 3/8-24 8,433 .3320 — Q — 12405 TDS411A08433
M10 x 1,50 — 8,500 .3346 — — 12735 12427 TDS411A08500
M10 x 1,00 — 9,000 .3543 — — 12736 12746 TDS411A09000
— 7/16-14 9,093 .3580 — T 12708 12406 TDS411A09093
M12 x 1,75 — 10,200 .4016 — — 12737 12428 TDS411A10200
M12 x 1,50 — 10,500 .4134 — — 12738 12747 TDS411A10500
— 1/2-13 10,716 .4219 27/64 — 12709 12407 TDS411A10716
— 1/2-20 11,509 .4531 29/64 — — 12408 TDS411A11509
M14 x 2,00 — 12,000 .4724 — — 12739 12429 TDS411A12000
— 9/16-12 12,304 .4844 31/64 — 12710 12409 TDS411A12304
M14 x 1,50 — 12,500 .4921 — — 12740 12748 TDS411A12500
— 5/8-11 13,495 .5313 17/32 — 12711 12410 TDS411A13495
M16 x 2,00 — 14,000 .5512 — — 12741 12430 TDS411A14000
M18 x 2,50 — 15,500 .6102 — — — 12431 TDS411A15500
— 3/4-10 16,670 .6563 21/32 — 12712 12411 TDS411A16670
M20 x 2,50 — 17,500 .6890 — — — 12432 TDS411A17500
required
tap drill diameter
blind hole approximately 3 x D
with coolant through hole with coolant
A26
WWW.WIDIA.COM
Page 26
High-Performance Taps
Cross Reference Chart • Solid Carbide Taps and Drills
K
Recommended SC Drill
approximately 5 x D approximately 5 x D approximately 5 x D approximately 5 x D
with coolant non-coolant with coolant non-coolant
TDS412 WK15PD TDS212 WK15PD VDS402A WU25PD VDS202A WU25PD
TDS402A02705 TDS212A02705 VDS402A02705 VDS202A02705
TDS402A03300 TDS212A03300 VDS402A03300 VDS202A03300
TDS402A03454 TDS212A03454 VDS402A03454 VDS202A03454
TDS402A03734 TDS212A03734 VDS402A03734 VDS202A03734
TDS402A04039 TDS212A04039 VDS402A04039 VDS202A04039
TDS402A04200 TDS212A04200 VDS402A04200 VDS202A04200
TDS402A05000 TDS212A05000 VDS402A05000 VDS202A05000
TDS402A05106 TDS212A05106 VDS402A05106 VDS202A05106
TDS402A05410 TDS212A05410 VDS402A05410 VDS202A05410
TDS402A06528 TDS212A06528 VDS402A06528 VDS202A06528
TDS412A06700 TDS212A06700 VDS412A06700 VDS212A06700
TDS412A07938 TDS212A07938 VDS412A07938 VDS212A07938
TDS412A08433 TDS212A08433 VDS412A08433 VDS212A08433
TDS412A08500 TDS212A08500 VDS412A08500 VDS212A08500
TDS412A09000 TDS212A09000 VDS412A09000 VDS212A09000
TDS412A09093 TDS212A09093 VDS412A09093 VDS212A09093
TDS412A10200 TDS212A10200 VDS412A10200 VDS212A10200
TDS412A10500 TDS212A10500 VDS412A10500 VDS212A10500
TDS412A10716 TDS212A10716 VDS412A10716 VDS212A10716
TDS412A11509 TDS212A11509 VDS412A11509 VDS212A11509
TDS412A12000 TDS212A12000 VDS412A12000 VDS212A12000
TDS412A12304 TDS212A12304 VDS412A12304 VDS212A12304
TDS412A12500 TDS212A12500 VDS412A12500 VDS212A12500
TDS412A13495 TDS212A13495 VDS412A13495 VDS212A13495
TDS412A14000 TDS212A14000 VDS412A14000 VDS212A14000
TDS412A15500 TDS212A15500 VDS412A15500 VDS212A15500
TDS412A16670 TDS212A16670 VDS412A16670 VDS212A16670
TDS412A17500 TDS212A17500 VDS412A17500 VDS212A17500
All Materials
Alternate Tap Drill
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A27
Page 27
High-Performance Taps
Cross Reference Chart • Solid Carbide Taps and Drills
Aluminum
Solid Carbide Taps
N
Solid Carbide Taps
typical
thread sizes
cutting taps
metric inch metric inch mm inch fraction wire GX47_GN1515 GX46_GN1515 GX49_GN1515
— — — 6-32 3,175 .1250 1/8 — — — 12895
M4,5 x 0,75 — M4 x 0,70 — 3,700 .1457 — — — — 12906
— — — 8-32 3,797 .1495 — 25 — — 12896
— — — 10-24 4,366 .1719 11/64 — — — 12897
12-24 — — 10-32 4,496 .1770 — 16 — — 12898
— — M5 x 0,80 — 4,700 .1850 — 13 — — 12907
M6 x 1,00 — — — 5,000 .1969 — — 12866 12846 —
— 1/4-20 — 12-28 5,106 .2010 — 7 12858 12836 —
— 1/4-28 — — 5,410 .2130 — 3 12859 12838 —
Holemaking • High-Performance Taps
— — M6 x 1,00 — 5,600 .2205 — — — — 12908
— — — 1/4-20 5,791 .2280 — 1 — — 12899
— — — 1/4-28 5,944 .2340 — A — — 12901
— 5/16-18 — — 6,528 .2570 — F 12860 12839 —
M8 x 1,25 — — — 6,700 .2638 — — 12867 12847 —
— — — 5/16-18 7,366 .2900 — L — — 12902
— — M8 x 1,25 — 7,400 .2913 — — — — 12909
— 3/8-16 — — 7,938 .3125 5/16 — 12861 12840 —
M10 x 1,50 — — — 8,500 .3346 — — 12868 12848 —
M10 x 1,00 — — — 9,000 .3543 — — 12869 12850 —
— — — 3/8-16 8,839 .3480 — S — — 12903
7/16-14 — — 3/8-24 9,093 .3580 — T 12862 12841 —
— — M10 x 1,50 — 9,400 .3701 — — — — 12911
M12 x 1,75 — — — 10,200 .4016 — — 12870 12851 —
M12 x 1,50 — — — 10,500 .4134 — — 12872 12852 —
— 1/2-13 — — 10,716 .4219 27/64 — 12863 12843 —
M14 x 2,00 — — — 12,000 .4724 — — 12873 12853 —
— 9/16-12 — — 12,304 .4844 31/64 — 12864 12844 —
M14 x 1,50 — — — 12,500 .4921 — — 12874 12854 —
— 5/8-11 — 9/16-12 13,495 .5313 17/32 — 12865 12845 —
M16 x 2,00 — — — 14,000 .5512 — — 12875 12855 —
M16 x 1,50 — — — 14,500 .5709 — — 12876 12856 —
forming taps
required
tap drill diameter
blind hole through hole forming blind hole
with coolant with coolant with coolant
A28
WWW.WIDIA.COM
Page 28
High-Performance Taps
Cross Reference Chart • Solid Carbide Taps and Drills
N
Solid Carbide Taps
forming through hole approximately 3 x D approximately 5 x D approximately 5 x D approximately 5 x D
with coolant with coolant with coolant with coolant non-coolant
GX48_GN1515 WD 412522 WD 412527 VDS402A WU25PD VDS202A WU25PD
12877 TCM65903000 012535—00318 VDS402A03175 VDS202A03175
12887 TCM25903700 — VDS402A03700 VDS202A03700
12878 — — VDS402A03797 VDS202A03797
12879 — — VDS402A04219 VDS202A04219
12880 — — VDS402A04496 VDS202A04496
12888 TCM25904700 — VDS402A04700 VDS202A04700
— TCM25909500 012535—00500 VDS402A05000 VDS202A05000
— — — VDS402A05106 VDS202A05106
— — — VDS402A05410 VDS202A05410
12889 TCM25905600 — VDS402A05600 VDS202A05600
12881 — — VDS402A05791 VDS202A05791
12882 — — VDS402A05944 VDS202A05944
— — — VDS402A06528 VDS202A06528
— TCM25906700 — VDS412A06700 VDS212A06700
12883 — — VDS412A07366 VDS212A07366
12890 TCM25907400 — VDS412A07400 VDS212A07400
— TCM65908000 012535—00793 VDS412A07938 VDS212A07938
— TCM25908500 012535—00850 VDS412A08500 VDS212A08500
— TCM25909000 012535—00900 VDS412A09000 VDS212A09000
12884 — — VDS412A08839 VDS212A08839
— — — VDS412A09093 VDS212A09093
12891 TCM25909400 — VDS412A09400 VDS212A09400
— TCM25910200 012535—01020 VDS412A10200 VDS212A10200
— TCM25910500 012535—01050 VDS412A10500 VDS212A10500
— — 012535—01072 VDS412A10716 VDS212A10716
— TCM25912000 012535—01200 VDS412A12000 VDS212A12000
— TCM65912100 — VDS412A12304 VDS212A12304
— TCM25912500 012535—01250 VDS412A12500 VDS212A12500
— — — VDS412A13495 VDS212A13495
— TCM25914000 012535—01400 VDS412A14000 VDS212A14000
— TCM25914500 012535—01450 VDS412A14500 VDS212A14500
Recommended SC Drill
All Materials
Alternate Tap Drill
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A29
Page 29
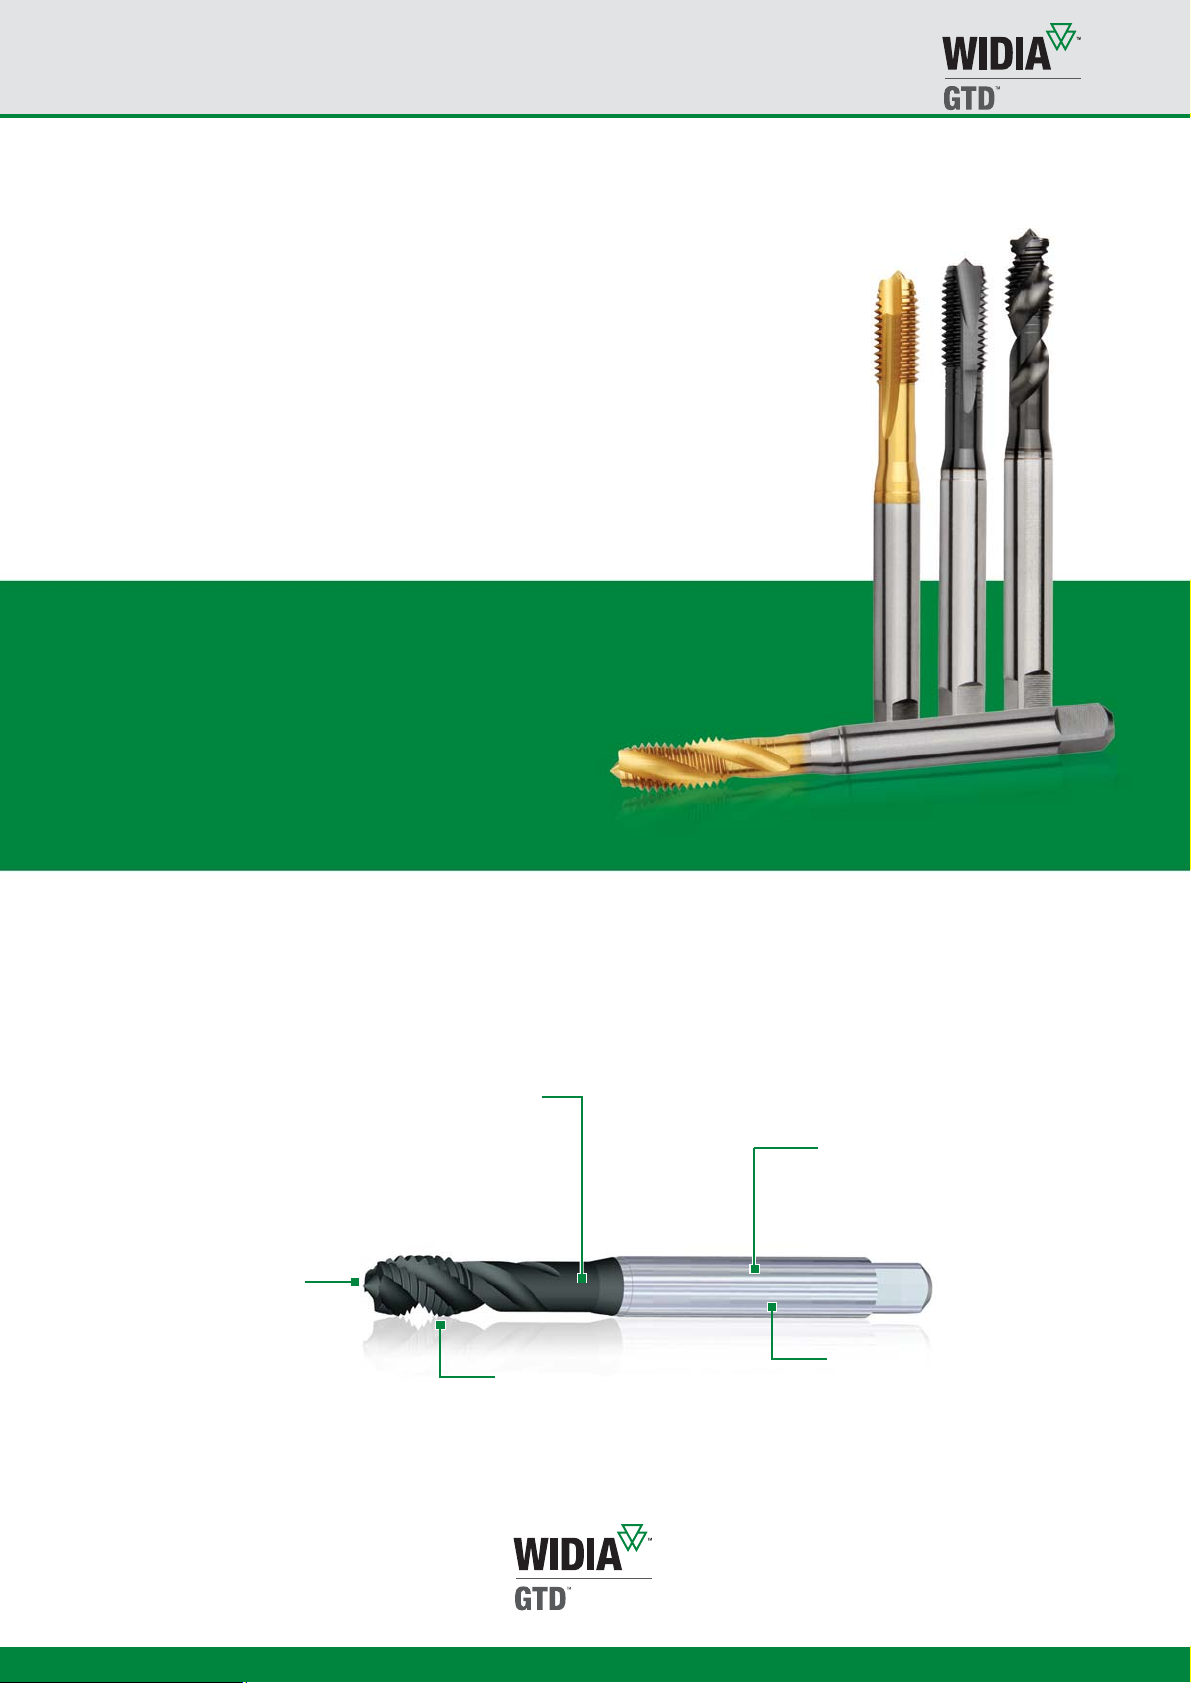
High-Performance HSS-E-PM Taps
Our powdered metal taps deliver highly reliable threads and superior
performance in blind and through hole applications. The HP HSS-E-PM is the
optimum choice for customers looking for high productivity and long tool life
in material-specific applications.
™
WIDIA-GTD
• Enhanced design for reliable thread on different materials.
• More resistant to edge chipping than carbide.
• Better performance at high speeds.
DIN standard
Longer tap reach, neck design,
better coolant flow.
Chamfer design
Helps chip load,
lower torque.
Various multilayer coatings
Extremely high wear resistance,
longer tool life.
Powdered metal substrate
Longer life, higher speed.
h6 or h9 shank
Low runout, h6 available
on some styles.
A30
WWW.WIDIA.COM
Page 30
Powdered Metal Taps
• Manufactured from high-speed steel and powder coated for thread
forming and thread cutting in various applications.
• Offer performance advantages over other regular high-speed taps.
• Unmatched by competitive products.
Tap Functions
• High wear resistance and hot hardness without sacrificing edge strength.
• PVD multilayer coatings offer outstanding thermal stability, hot hardness,
oxidation resistance, and low frictional coefficient.
• Spiral point feature pushes chips ahead in through holes.
• Chips stored in flutes or flushed out with straight flutes.
• Taps can be used in collet and hydraulic holders.
• Low runout of thread and chamfer.
Benefits
• Long tap life at up to 50% higher tapping speed.
• Excellent chip control.
• Greater thread strength.
• Exceptional thread quality and long life.
WWW.WIDIA.COM
A31
Page 31
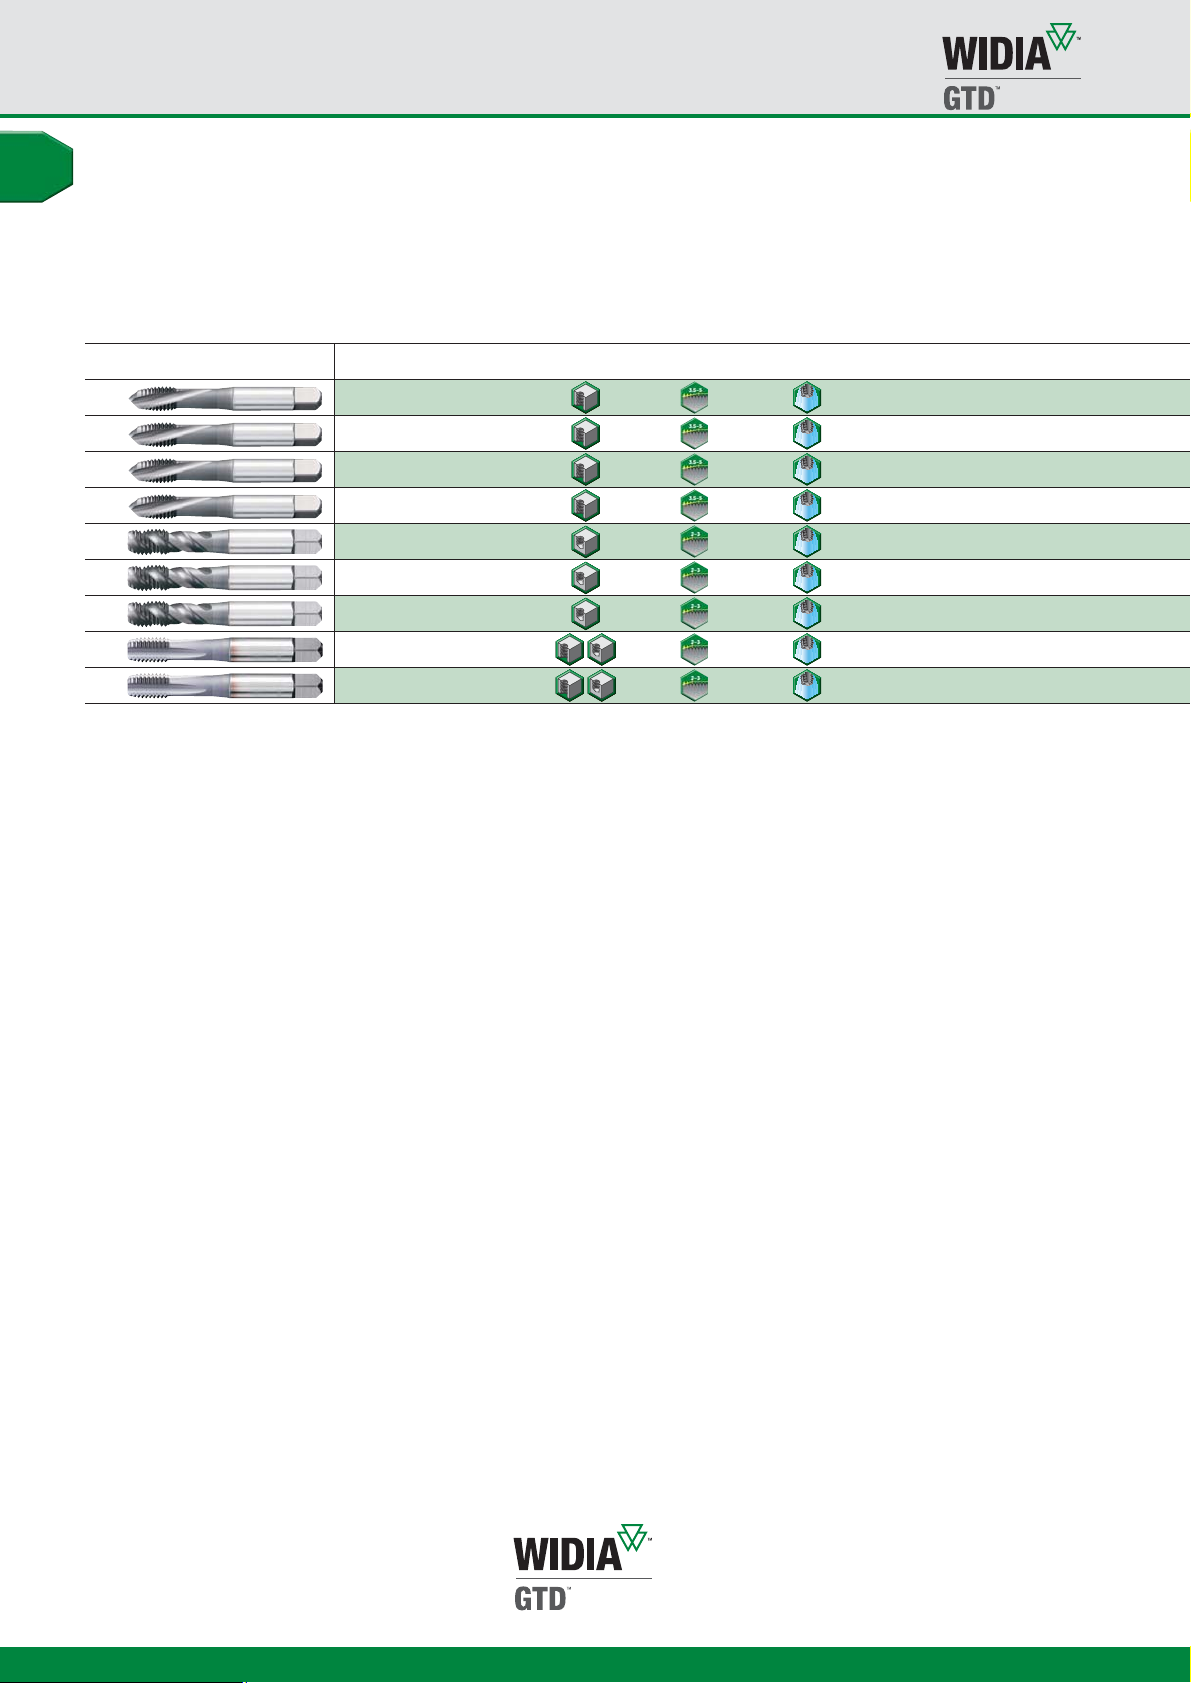
High-Performance Taps
Taps Selection Guide • HSS-E-PM Taps
Victory™GT Series HSS-E-PM Taps • ANSI Inch and Metric
Good
多
Better
多多
Best
多多多
GT Series High-Performance
HSS-E-PM Taps
series
GT20
size range
(inch and metric)
size
min - max
#2 - 3/4" GP6520 ANSI 302A
hole
chamfer
form
coolant grade
tap
dimension
Holemaking • High-Performance Taps
GT20
GT20
GT20
GT30
GT30
GT30
GT40
GT40
#2 - 3/4" GM6515 ANSI 302A
M3 - M12 GP6520 ANSI 302A
M3 - M12 GM6515 ANSI 302A
#2 - 1" GP6520 ANSI 302A
#2 - 1" GM6515 ANSI 302A
#4 - 3/4" GP6505 ANSI 302A
#10 - 3/4" GP6520 ANSI 302A
M3 - M16 GP6520 ANSI 302A
A32
WWW.WIDIA.COM
Page 32
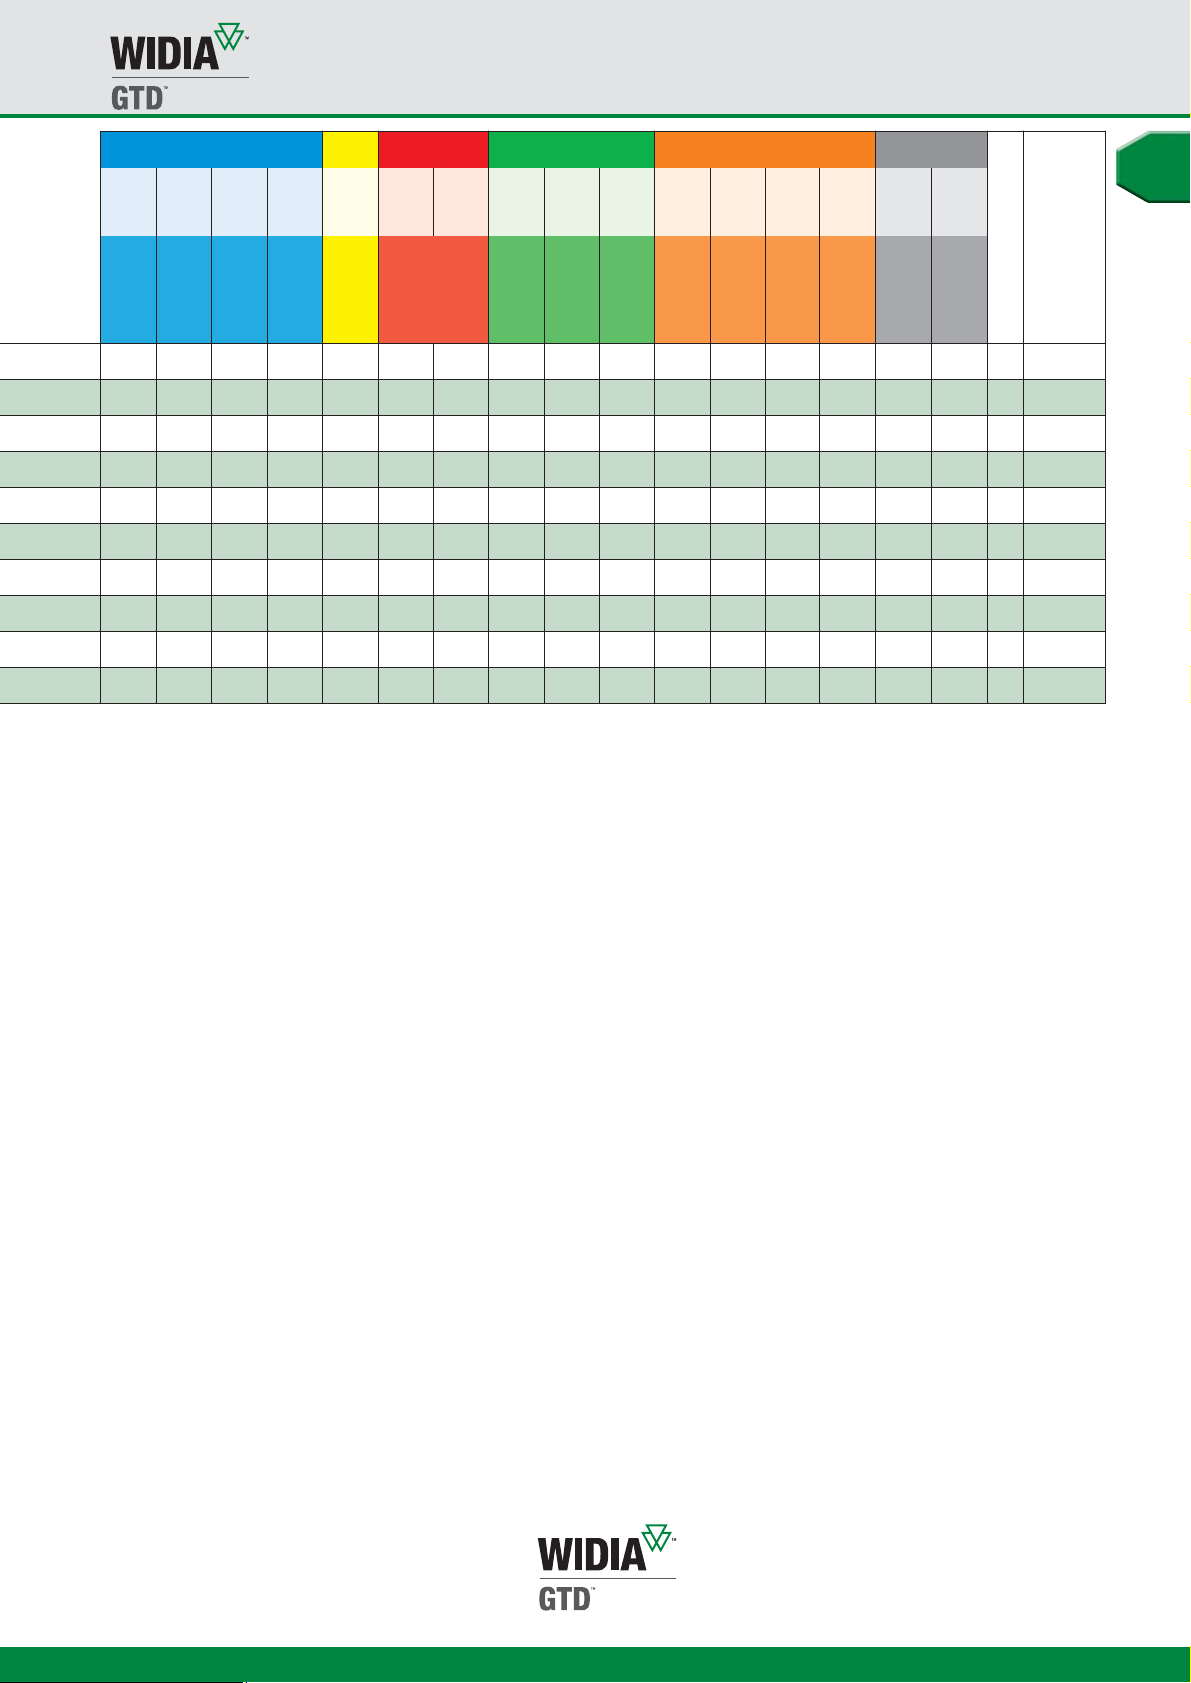
High-Performance Taps
Taps Selection Guide • HSS-E-PM Taps
P M K N S H
1, 2, 3,
<35 HRC
4, 6, 7
Steel
5, 9,
10, 11
Steel
36–48
HRC
12, 13.1 13.2
PH &
Steel
PH &
Ferriitic
Stainless
Steel
>35 HRC
Ferriitic
Stainless
<35 HRC
14.1, 14.2,
14.3, 14.4
Stainless
Steel
15, 16,
17, 18, 19
Cast Iron
20 21
Wrought
Aluminum
22, 23,
24, 25
Cast
Aluminum
26, 27,
28
Copper,
Copper
Alloys
31, 32
Iron
Based
多多多 多多多 多多多
多多多 多 多 多
多多多 多多多 多多多
多多多 多 多 多
多多多 多多多 多多多
多多多 多 多 多
多多 多 多
多多多 多多多
多多多 多多多
33, 34,
35
Cobalt
Based
36 37
Nickel
Based
Titanium
& Alloys
38.1, 38.2,
40.1, 40.2,
41.1
Hardened
Steel
49–55
HRC
39.1,
41.2
Hardened
Steel
56–68
HRC
Recommended
Page
Cutting
Parameters
A36 A70–A71
A36 A70–A71
A37 A70–A71
A37 A70–A71
A44 A70–A71
A44 A70–A71
A56 A70–A71
A57 A70–A71
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A33
Page 33
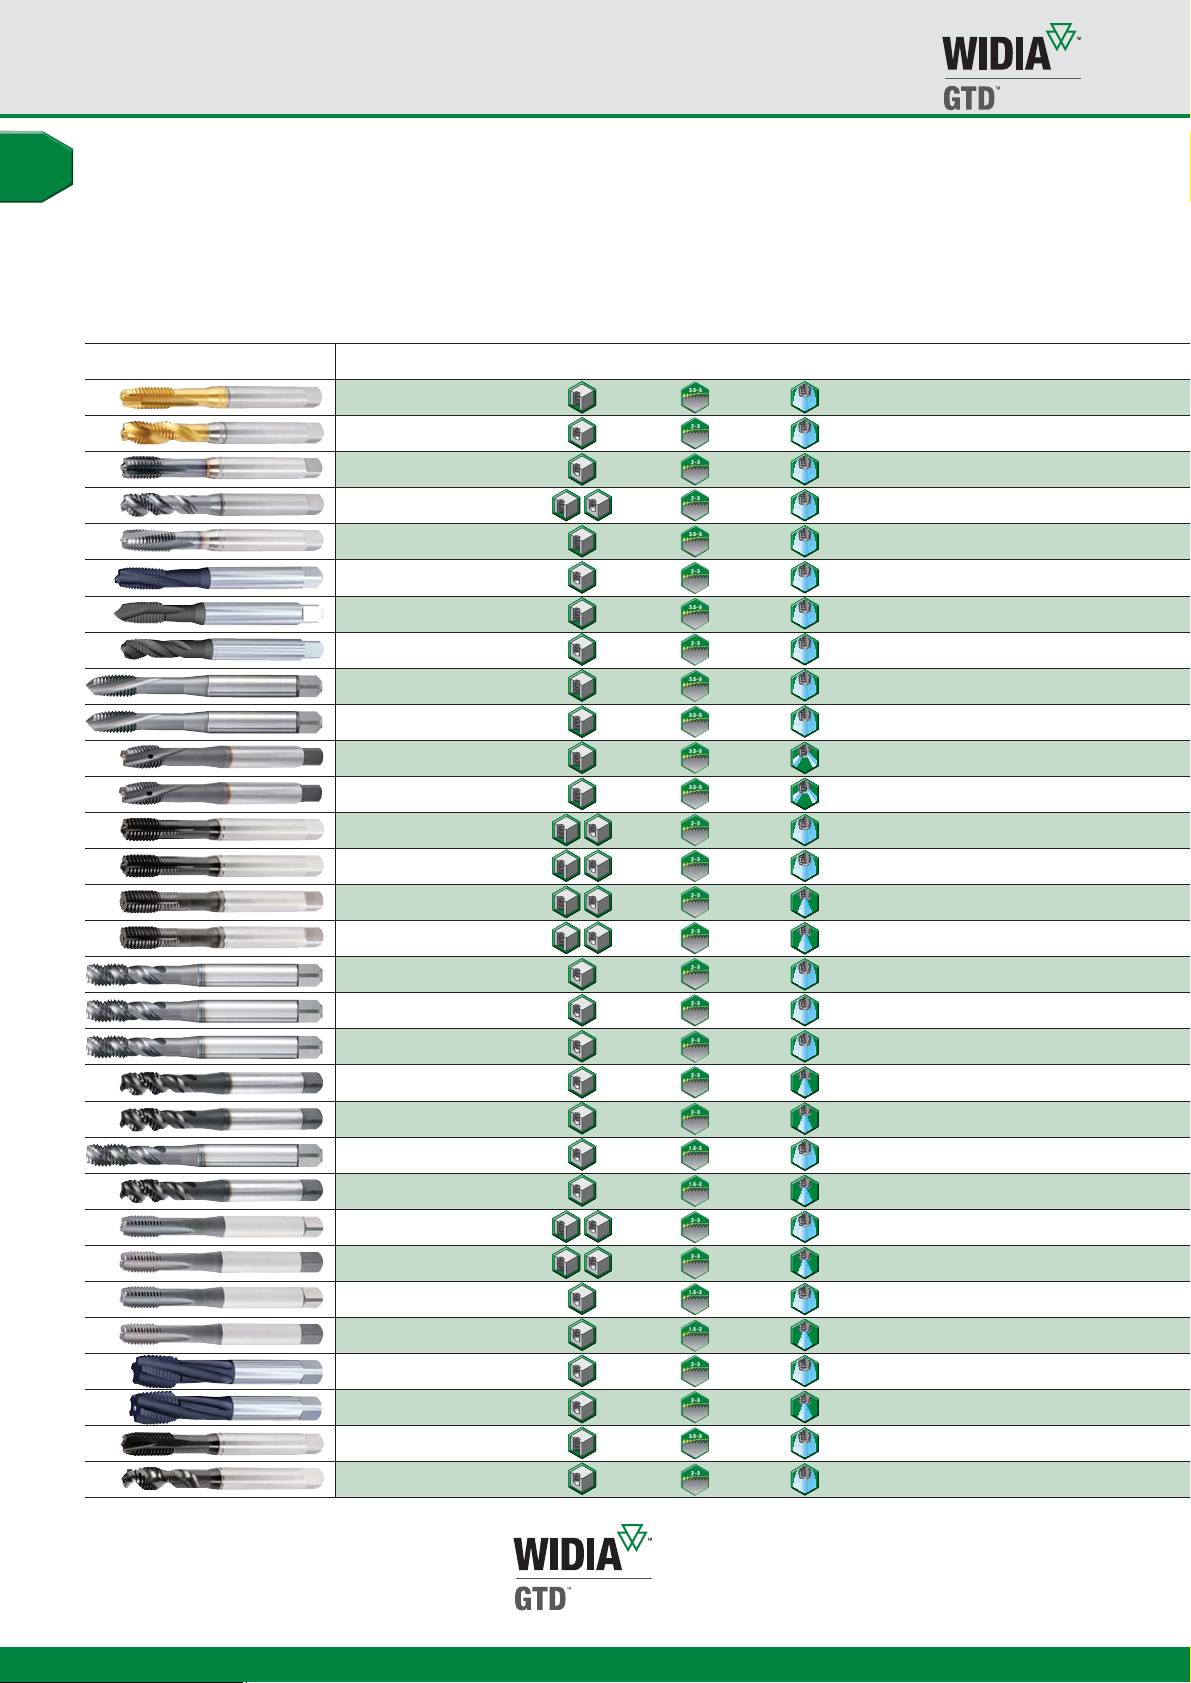
High-Performance Taps
Taps Selection Guide • HSS-E-PM Taps
Victory™GT Series HP HSS-E-PM Taps • DIN Metric
Good
多
Better
多多
Best
多多多
GT Series High-Performance
HSS-E-PM Taps
series grade
GT00
size range
(metric)
size
min - max
M3 - M20
hole
chamfer
form
coolant
tap
dimension
WP31MG DIN 371,374,376
Holemaking • High-Performance Taps
GT02
GT04
GT06
GT10
GT12
GT14
GT16
GT20
GT20
GT21
GT21
GT22
GT22
GT23
GT23
GT30
GT30
M3 - M20
M3 - M20
M6 - M16
M3 - M20
M3 - M20
M3 - M12
M3 - M12
M3 - M42
M3 - M20
M5 - M14
M5 - M14
M3 - M16
M3 - M16
M5 - M16
M5 - M16
M3 - M42
M3 - M24
WP31MG DIN 371,374,376
WH36MG DIN 371,374,376
WS32MG DIN 371,374,376
WS32MG DIN 371,374,376
WS32MG DIN 371,374,376
WN35MG DIN 371,376
WN35MG DIN 371
GP6520 DIN 371,374,376,XL
GM6515 DIN 371,374,376
GP6520 DIN 371,376
GM6515 DIN 371,376
WP31MG DIN 371,374,376
WN38MG DIN 371,374,376
WP31MG DIN 371,374,376
WN38MG DIN 371,374,376
GP6520 DIN 371,374,376,XL
GM6515 DIN 371,374,376
A34
GT30
GT31
GT31
GT32
GT33
GT40
GT41
GT42
GT43
GT50
GT51
GT70
GT80
M3 - M16
M5 - M42
M5 - M16
M5 - M16
M5 - M16
M4 - M22
M4 - M20
M5 - M16
M5 - M16
M24 - M42
M24 - M42
M3 - M16
M3 - M20
GP6505 DIN 371,376
GP6520 DIN 371,376,XL
GM6515 DIN 371,376
GP6520 DIN 371,374,376
GP6520 DIN 371,374,376
GP6520 DIN 371,376
GP6520 DIN 371,376
GP6520 DIN 371,374,376
GP6520 DIN 371,374,376
GP6520 DIN 376,XL
GP6520 DIN 376,XL
WN48EG DIN 371,376
WN48EG DIN 371,376
WWW.WIDIA.COM
Page 34
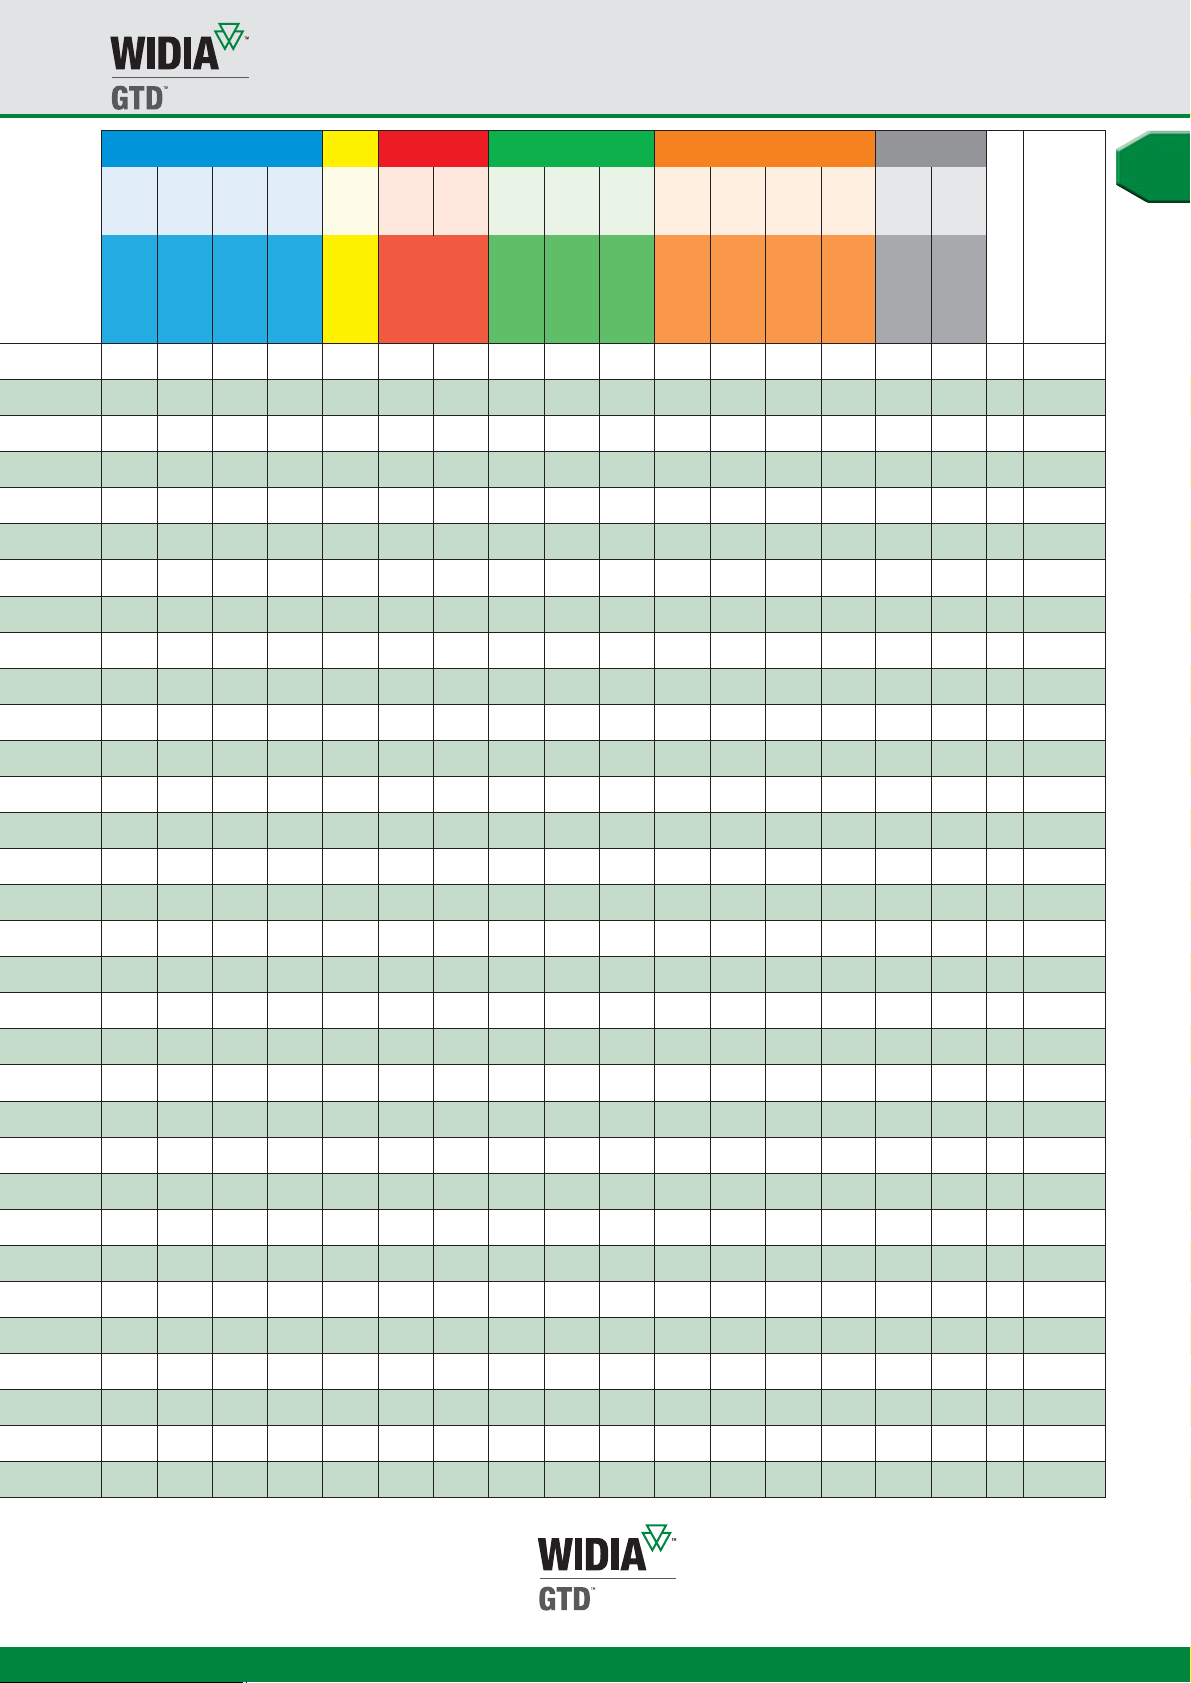
High-Performance Taps
Taps Selection Guide • HSS-E-PM Taps
P M K N S H
1, 2, 3,
<35 HRC
5, 9,
10, 11
Steel
36–48
HRC
12, 13.1 13.2
PH &
Ferriitic
Stainless
Steel
<35 HRC
4, 6, 7
Steel
多多多 多多多 多 多 多
多多多 多多多 多 多
多多多 多多多 多多多
PH &
Ferriitic
Stainless
Steel
>35 HRC
14.1, 14.2,
14.3, 14.4
Stainless
Steel
15, 16,
17, 18, 19
Cast Iron
20 21
Aluminum
Wrought
22, 23,
24, 25
Cast
Aluminum
26, 27,
28
Copper,
Copper
Alloys
多
多
多多多 多多 多多 多多
多多多 多多多
多多多
31, 32
Iron
Based
多 多多多
多 多多多
多多多 多多多 多多多
多多多 多 多 多
多多多 多多多 多多多
多多多 多 多 多
33, 34,
Cobalt
Based
36 37
35
Nickel
Based
多多多 多多多
多多多 多多多
Titanium
& Alloys
38.1, 38.2,
40.1, 40.2,
41.1
Hardened
Steel
49–55
HRC
39.1,
41.2
Hardened
Steel
56–68
HRC
Recommended
Page(s)
Cutting
Parameters
A40 A70–A71
A50 A70–A71
A52 A70–A71
A53 A70–A71
A42 A70–A71
A54 A70–A71
A43 A70–A71
A55 A70–A71
A38,
A70–A71
A65
A38 A70–A71
A39 A70–A71
A39 A70–A71
A62 A70–A71
Holemaking • High-Performance Taps
多多多 多多多 多
多多多
多多多 多
多多多 多多多 多多多
多多多 多 多
多多
多多多 多多多 多多多
多多多 多 多
多多多 多多多 多多多
多多多 多多多
多多多 多多多 多多
多多多
多多多 多多多 多多
多多多
多多多 多多多 多多
多多多
多多多 多多多 多多
多多多
多多多 多多 多
多多多 多多 多
多多多 多 多
多多多
A62 A70–A71
A63 A70–A71
A63 A70–A71
A46,
A70–A71
A66
A46 A70–A71
A46 A70–A71
A47,
A70–A71
A67
A47 A70–A71
A48 A70–A71
A49 A70–A71
A58 A70–A71
A59 A70–A71
A60 A70–A71
A61 A70–A71
A68 A70–A71
A69 A70–A71
A41 A70–A71
A51 A70–A71
WWW.WIDIA.COM
A35
Page 35
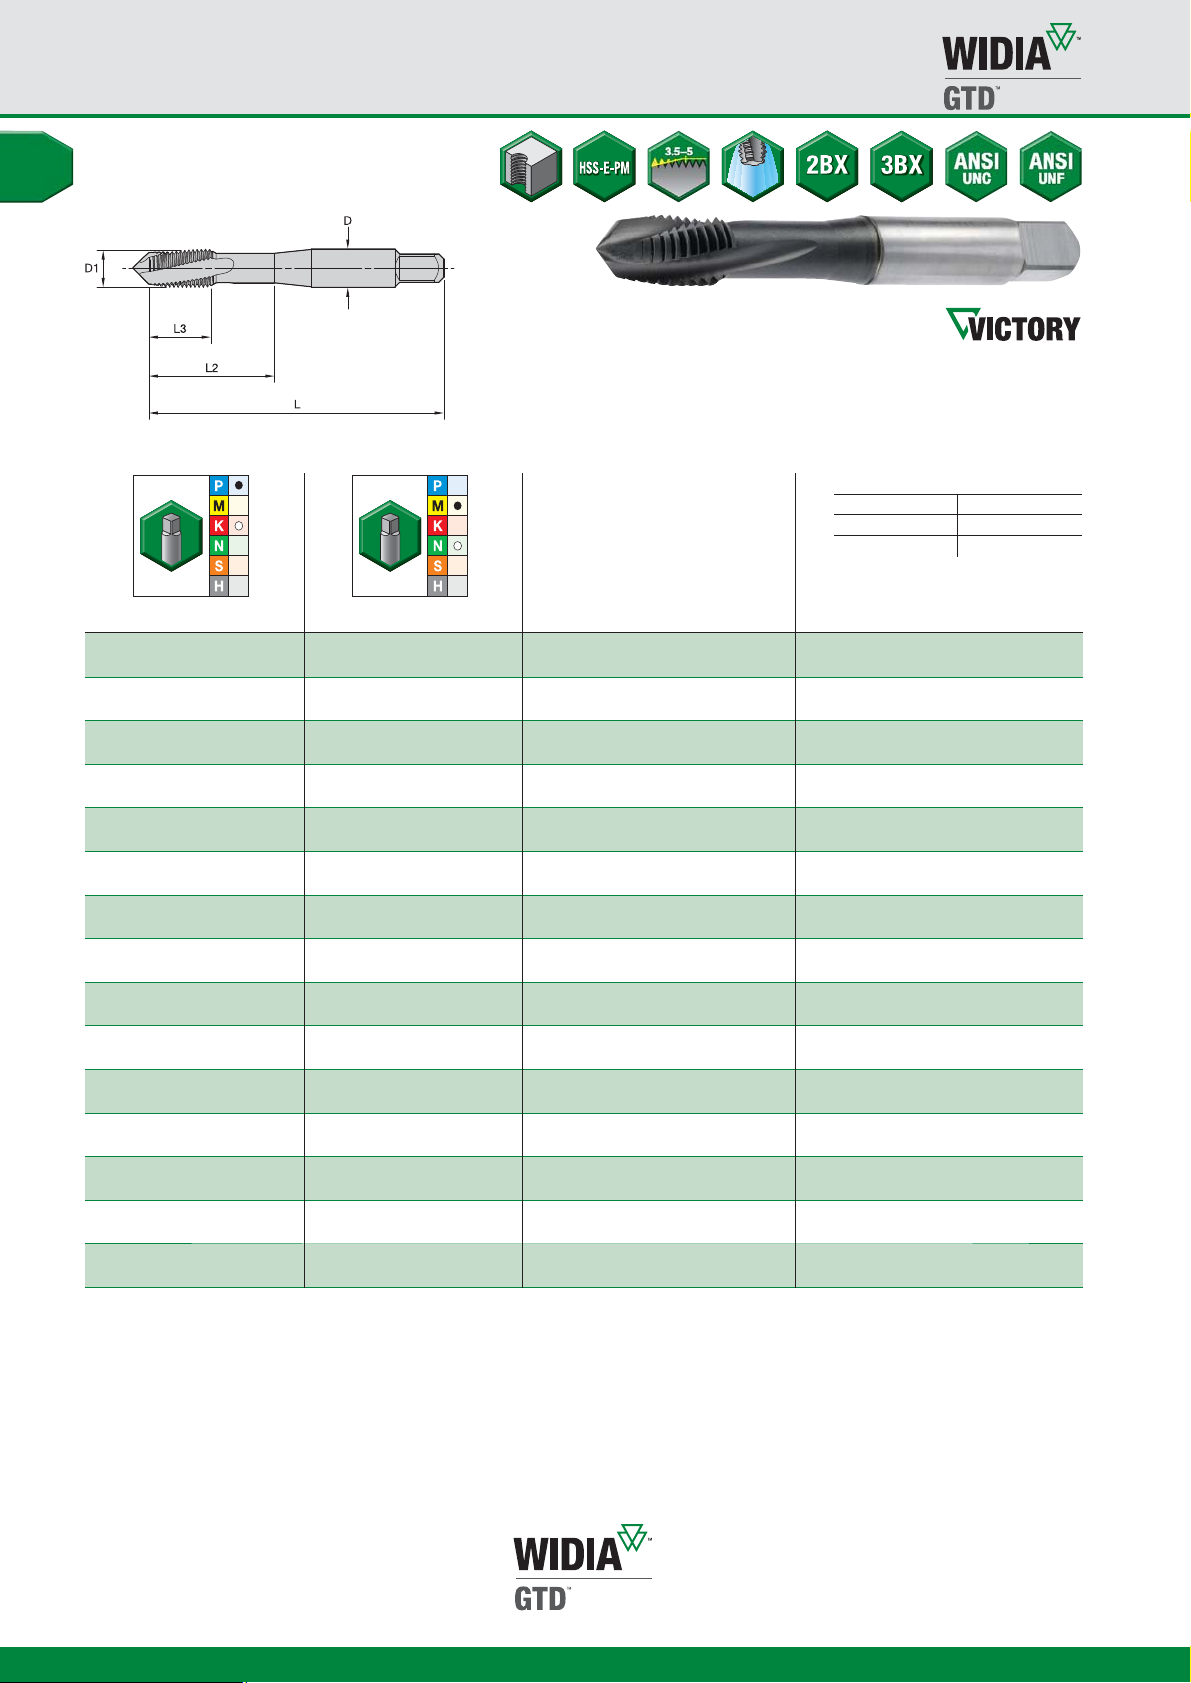
High-Performance Taps
Victory™Left-Hand Spiral-Flute HSS-E-PM Taps • Through Holes
• GM6515 TiN + CrC/C for
stainless steel.
• GP6520 TiCN for steel.
GT20 • Machine Screw and Fractional • Form D Plug Chamfer
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
D Fractional D Inch
.250–.375 +0, -.0004
.438–.625 +0, -.0004
Shank Tolerance
GP6520 GM6515 D1 size L L3 L2 D
GT205031 GT205001 2 - 56 1.75 .44 .50 .141 2 2BX
GT205032 GT205002 2 - 56 1.75 .44 .50 .141 2 3BX
GT205033 GT205003 4 - 40 1.88 .56 .69 .141 2 2BX
GT205034 GT205004 4 - 40 1.88 .56 .69 .141 2 3BX
GT205035 GT205005 5 - 40 1.94 .63 .75 .141 2 3BX
GT205036 GT205006 6 - 32 2.00 .36 .71 .141 2 2BX
GT205037 GT205007 6 - 32 2.00 .36 .71 .141 2 3BX
GT205038 GT205008 8 - 32 2.13 .31 .76 .168 2 2BX
GT205039 GT205009 8 - 32 2.13 .31 .76 .168 2 3BX
GT205052 GT205022 8 - 36 2.13 .31 .76 .168 3 3BX
GT205040 GT205010 10 - 24 2.38 .47 .91 .194 3 3BX
GT205053 GT205023 10 - 32 2.38 .47 .91 .194 3 2BX
GT205054 GT205024 10 - 32 2.38 .47 .91 .194 3 3BX
GT205041 GT205011 12 - 24 2.38 .42 .96 .220 3 3BX
GT205042 GT205012 1/4 - 20 2.50 .44 1.00 .255 3 2BX
GT205043 GT205013 1/4 - 20 2.50 .44 1.00 .255 3 3BX
GT205055 GT205025 1/4 - 28 2.50 .44 1.00 .255 3 2BX
GT205056 GT205026 1/4 - 28 2.50 .44 1.00 .255 3 3BX
GT205044 GT205014 5/16 - 18 2.72 .49 1.13 .318 3 2BX
GT205045 GT205015 5/16 - 18 2.72 .49 1.13 .318 3 3BX
GT205057 GT205027 5/16 - 24 2.72 .49 1.13 .318 3 3BX
GT205046 GT205016 3/8 - 16 2.94 .60 1.27 .381 3 2BX
GT205047 GT205017 3/8 - 16 2.94 .60 1.27 .381 3 3BX
GT205058 GT205028 3/8 - 24 2.94 .60 1.27 .381 3 3BX
GT205048 GT205018 7/16 - 14 3.16 .71 1.49 .323 3 3BX
GT205059 GT205029 7/16 - 20 3.16 .71 1.49 .323 3 3BX
GT205049 GT205019 1/2 - 13 3.38 .77 1.74 .367 3 3BX
GT205060 GT205030 1/2 - 20 3.38 .77 1.74 .367 3 3BX
GT205050 GT205020 5/8 - 11 3.81 .91 1.89 .480 3 3BX
GT205051 GT205021 3/4 - 10 4.25 1.00 2.08 .590 3 3BX
number
of flutes
class
of fit
A36
WWW.WIDIA.COM
Page 36
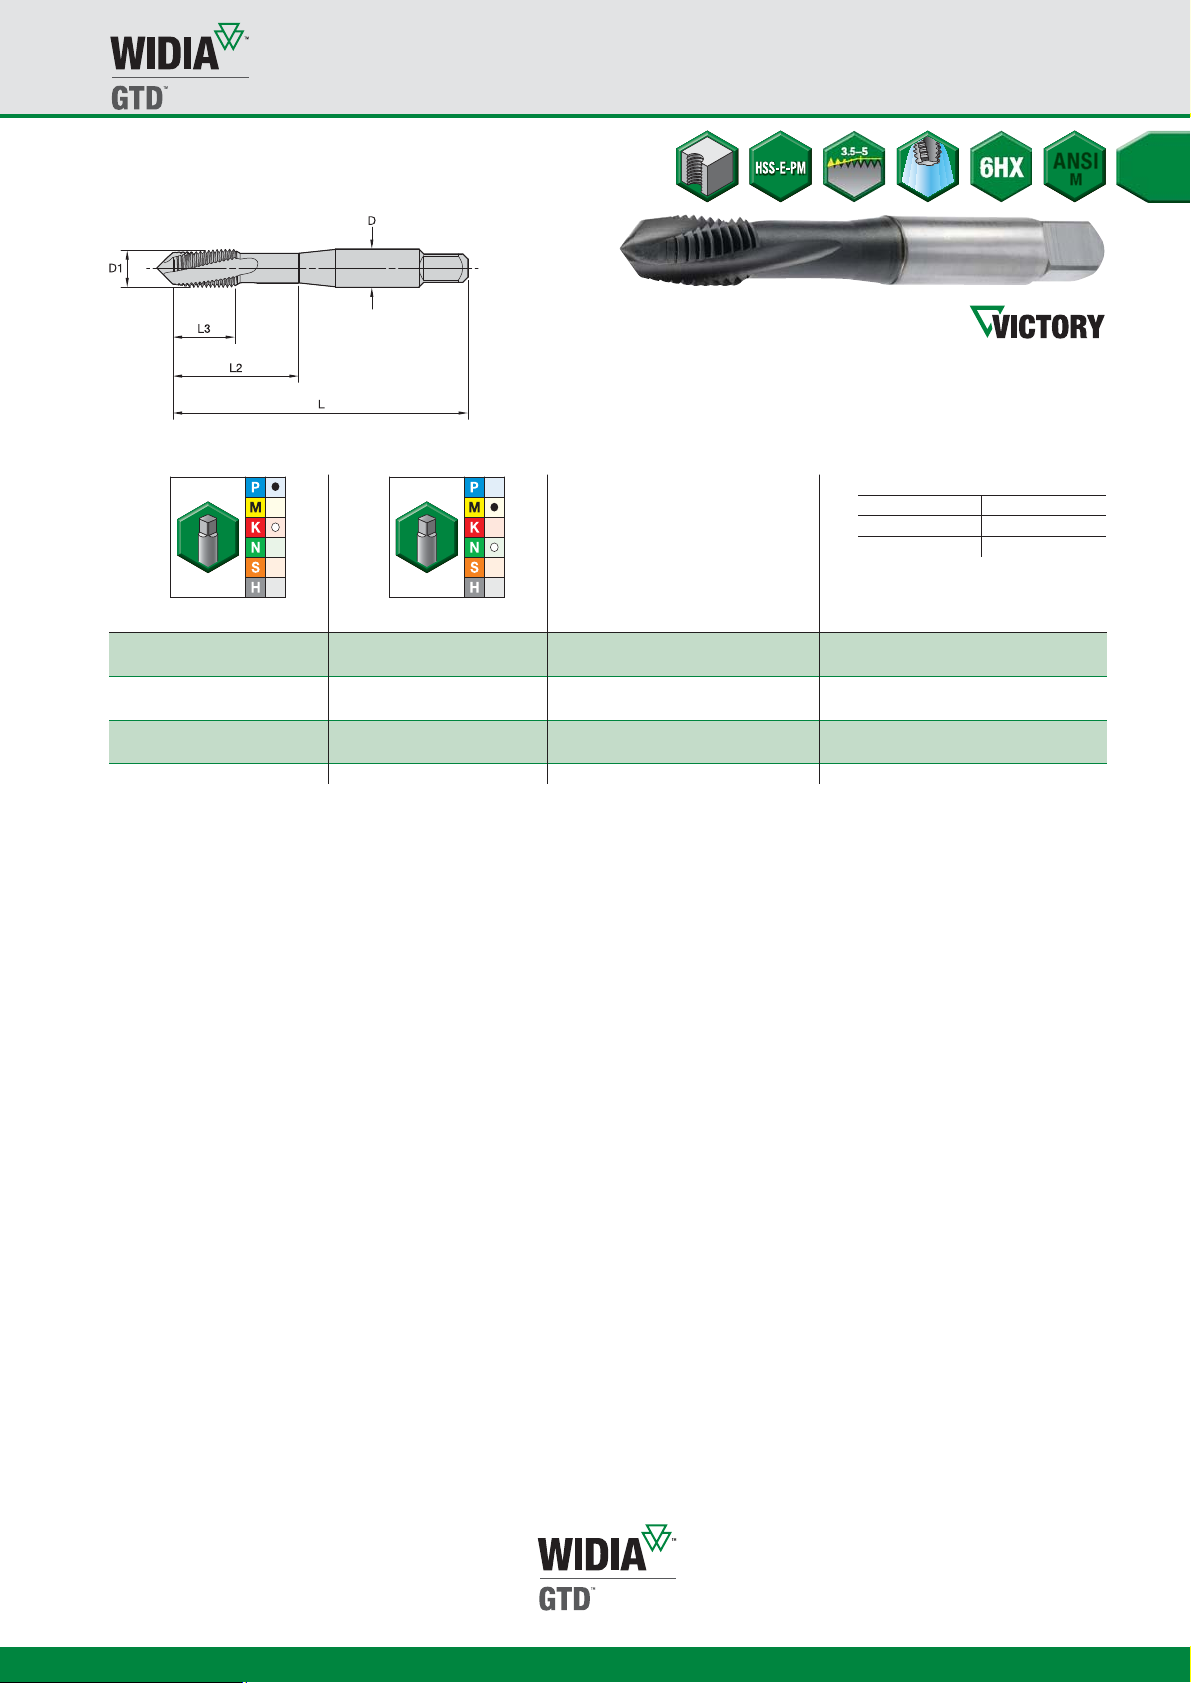
• GM6515 TiN + CrC/C for
stainless steel.
• GP6520 TiCN for steel.
GT20 • Form D Plug Chamfer • Metric ANSI
High-Performance Taps
Victory™Left-Hand Spiral-Flute HSS-E-PM Taps • Through Holes
ANSI
M
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Fractional D Inch
.250–.375 +0, -.0004
.438–.625 +0, -.0004
Holemaking • High-Performance Taps
GP6520 GM6515 D1 size L L3 L2 D
GT205069 GT205061 M3 X 0,5 1.94 .63 .75 .141 2 6HX
GT205070 GT205062 M4 X 0,7 2.13 .32 .76 .168 2 6HX
GT205071 GT205063 M5 X 0,8 2.38 .47 .91 .194 2 6HX
GT205072 GT205064 M6 X 1 2.50 .46 1.01 .255 3 6HX
GT205074 GT205066 M8 X 1,25 2.72 .48 1.12 .318 3 6HX
GT205075 GT205067 M10 X 1,5 2.94 .53 1.26 .381 3 6HX
GT205076 GT205068 M12 X 1,75 3.38 .77 1.74 .367 3 6HX
number
of flutes
class
of fit
WWW.WIDIA.COM
A37
Page 37
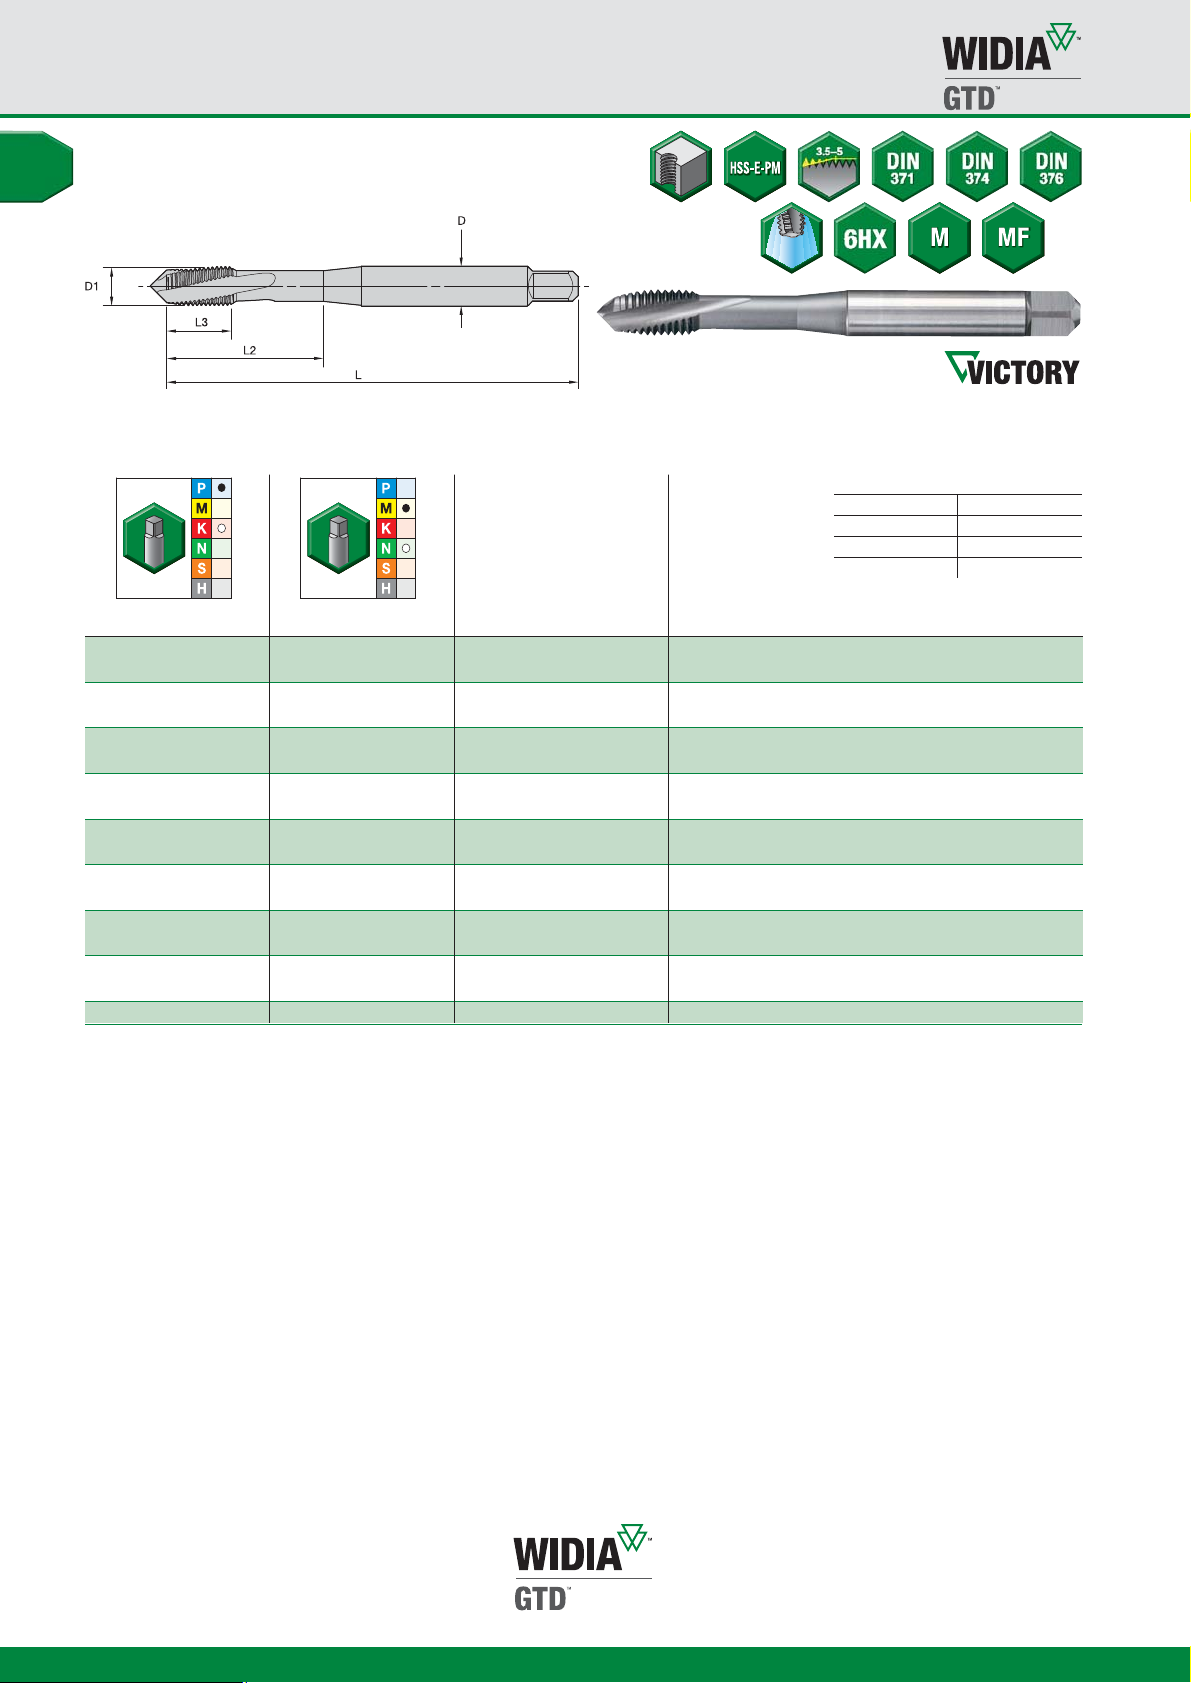
High-Performance Taps
Victory™Left-Hand Spiral-Flute HSS-E-PM Taps • Through Holes
• GM6515 TiN + CrC/C for stainless steel.
• GP6520 TiCN for steel.
GT20 • Form D Plug Chamfer • Metric DIN 371, 374, and 376
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
GP6520 GM6515 D1 size L L3 L2 D
GT205094 GT205077 M3 X 0,5 56 8 18 3,5 2 DIN 371 6HX
GT205095 GT205078 M4 X 0,7 63 10 21 4,5 2 DIN 371 6HX
GT205096 GT205079 M5 X 0,8 70 10 25 6,0 2 DIN 371 6HX
GT205097 GT205080 M6 X 1 80 10 30 6,0 3 DIN 371 6HX
GT205104 GT205087 M8 X 1 90 13 35 6,0 4 DIN 374 6HX
GT205098 GT205081 M8 X 1,25 90 13 35 8,0 3 DIN 371 6HX
GT205105 GT205088 M10 X 1 90 10 35 7,0 4 DIN 374 6HX
GT205106 GT205089 M10 X 1,25 100 15 39 7,0 4 DIN 374 6HX
GT205099 GT205082 M10 X 1,5 100 15 39 10,0 3 DIN 371 6HX
GT205107 GT205090 M12 X 1,5 100 15 39 9,0 4 DIN 374 6HX
GT205100 GT205083 M12 X 1,75 110 18 44 9,0 3 DIN 376 6HX
GT205108 GT205091 M14 X 1,5 100 15 47 11,0 4 DIN 374 6HX
GT205101 GT205084 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT205109 GT205092 M16 X 1,5 100 15 46 12,0 4 DIN 374 6HX
GT205102 GT205085 M16 X 2 110 20 51 12,0 4 DIN 376 6HX
GT205110 GT205093 M18 X 1,5 110 15 50 14,0 4 DIN 374 6HX
GT205103 GT205086 M20 X 2,5 140 25 64 16,0 4 DIN 376 6HX
number
of flutes
dimension
standard
class
of fit
A38
WWW.WIDIA.COM
Page 38
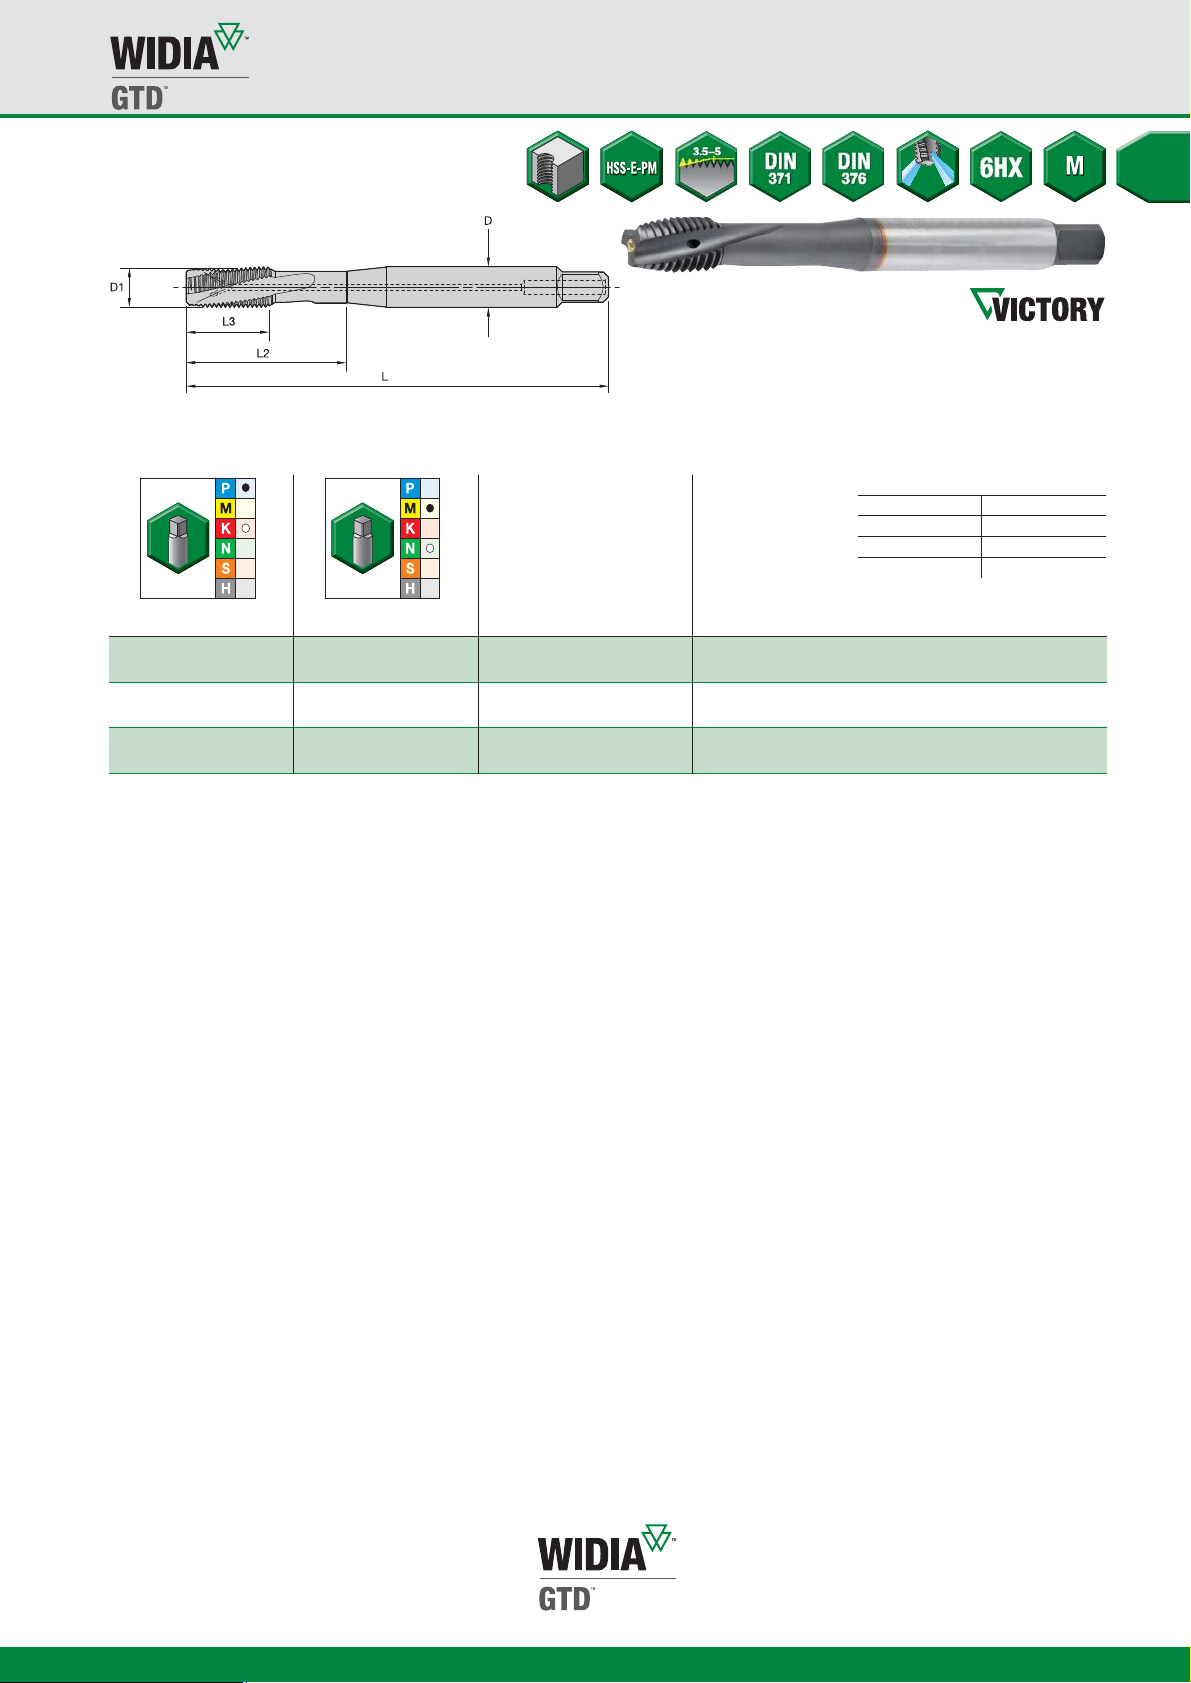
Victory™Left-Hand Spiral-Flute HSS-E-PM Taps • Through Holes
• GM6515 TiN+CrC/C for stainless steel.
• GP6520 TiCN for steel.
䢇
first choice
嘷
alternate choice
GT21 • Form D Plug Chamfer • Through Coolant • Metric DIN 371 and 376
High-Performance Taps
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
Holemaking • High-Performance Taps
GP6520 GM6515 D1 size L L3 L2 D
GT215007 GT215001 M5 X 0,8 70 10 25 6,0 2 DIN 371 6HX
GT215008 GT215002 M6 X 1 80 10 30 6,0 3 DIN 371 6HX
GT215009 GT215003 M8 X 1,25 90 13 35 8,0 3 DIN 371 6HX
GT215010 GT215004 M10 X 1,5 100 15 39 10,0 3 DIN 371 6HX
GT215011 GT215005 M12 X 1,75 110 18 44 9,0 3 DIN 376 6HX
GT215012 GT215006 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
number
of flutes
dimension
standard
class
of fit
WWW.WIDIA.COM
A39
Page 39
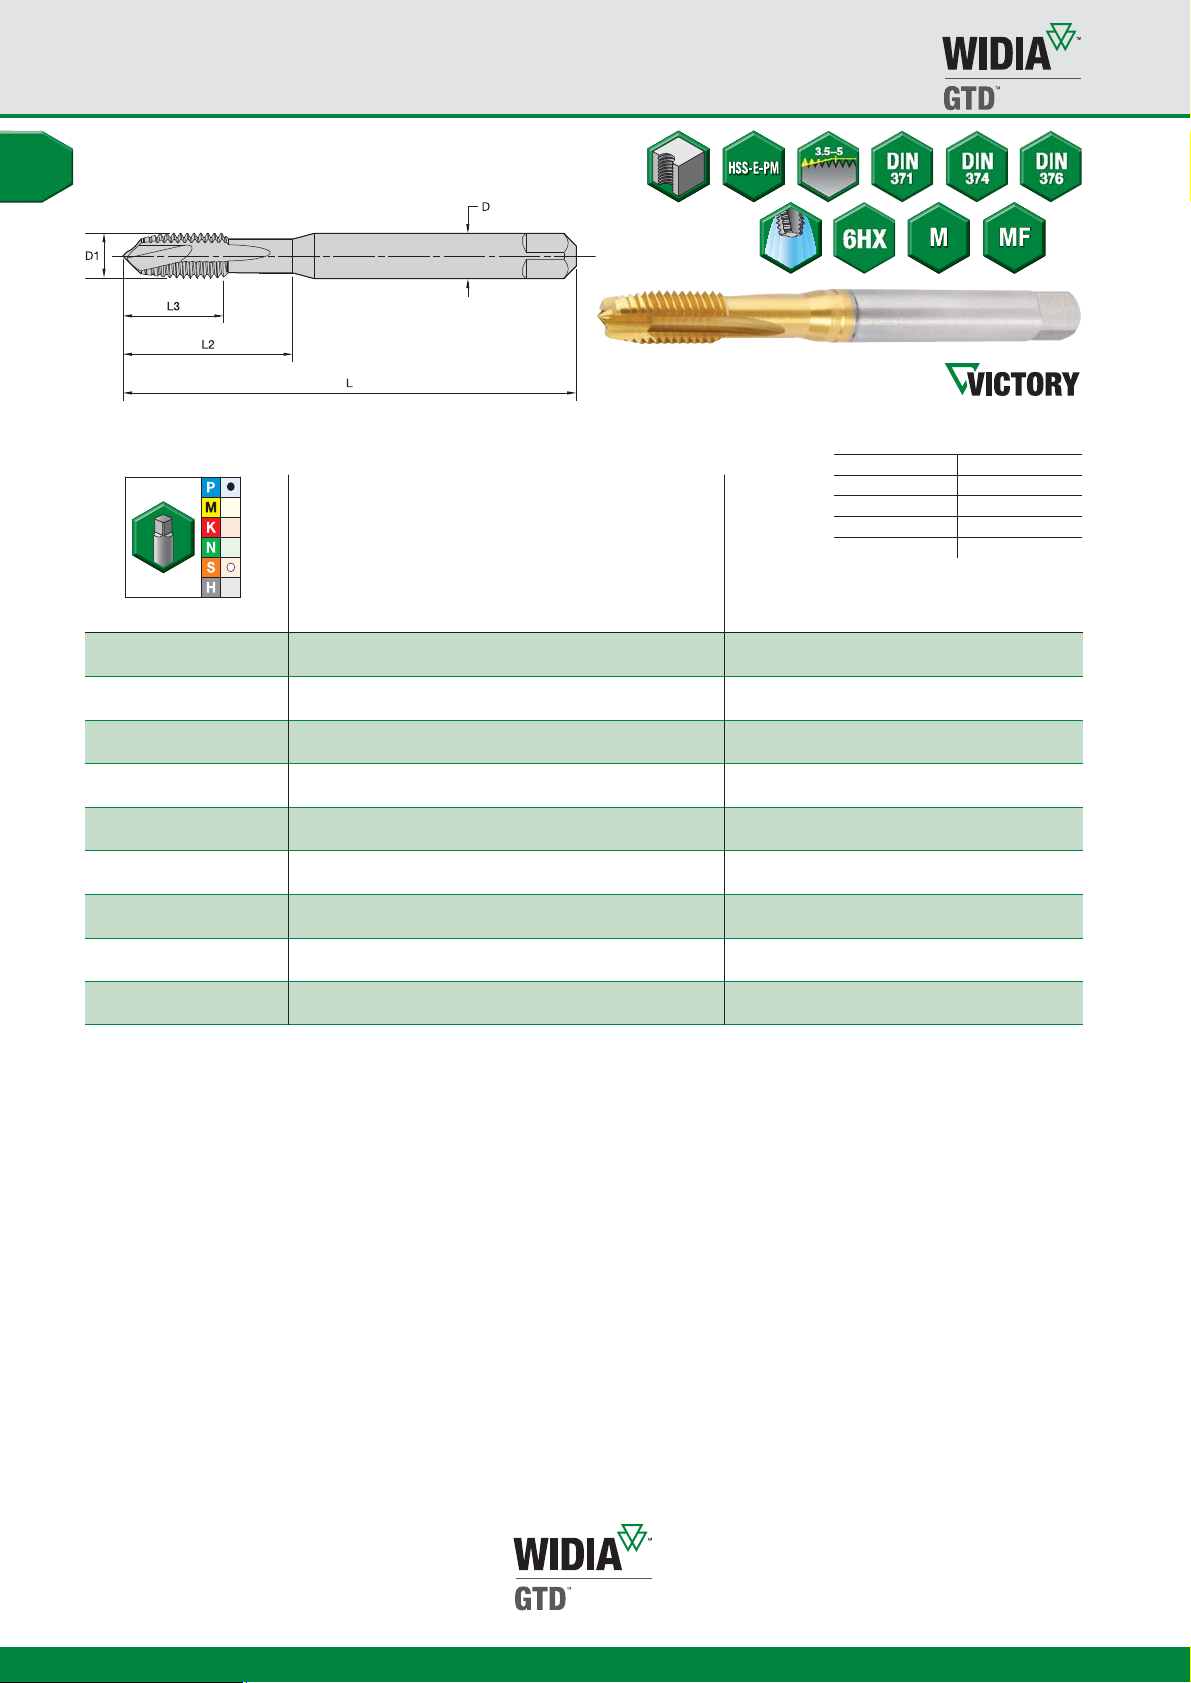
High-Performance Taps
Victory™Spiral-Point Plug HSS-E-PM Taps • Through Holes
• WP31MG TiN for steel 32–44 HRC.
䢇
first choice
嘷
alternate choice
Holemaking • High-Performance Taps
GT00 • Form B Plug Chamfer • Metric DIN 371, 374, and 376
WP31MG D1 size L L3 L2 D
GT005001 M3 X 0,5 56 11 18 3,5 2 DIN 371 6HX
GT005002 M4 X 0,7 63 13 21 4,5 2 DIN 371 6HX
GT005003 M5 X 0,8 70 15 25 6,0 2 DIN 371 6HX
GT005004 M6 X 1 80 17 30 6,0 3 DIN 371 6HX
GT005012 M8 X 1 90 17 — 6,0 3 DIN 374 6HX
GT005005 M8 X 1,25 90 20 35 8,0 3 DIN 371 6HX
GT005013 M10 X 1 90 18 — 7,0 3 DIN 374 6HX
GT005014 M10 X 1,25 100 22 — 7,0 3 DIN 374 6HX
GT005006 M10 X 1,5 100 22 39 10,0 3 DIN 371 6HX
GT005015 M12 X 1,25 100 22 — 9,0 3 DIN 374 6HX
GT005016 M12 X 1,5 100 22 — 9,0 3 DIN 374 6HX
GT005007 M12 X 1,75 110 24 — 9,0 3 DIN 376 6HX
GT005017 M14 X 1,5 100 22 — 11,0 3 DIN 374 6HX
GT005008 M14 X 2 110 26 — 11,0 3 DIN 376 6HX
GT005018 M16 X 1,5 100 22 — 12,0 4 DIN 374 6HX
GT005009 M16 X 2 110 27 — 12,0 4 DIN 376 6HX
GT005010 M18 X 2 125 30 — 14,0 4 DIN 376 6HX
GT005011 M20 X 2,5 140 32 — 16,0 4 DIN 376 6HX
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
A40
WWW.WIDIA.COM
Page 40
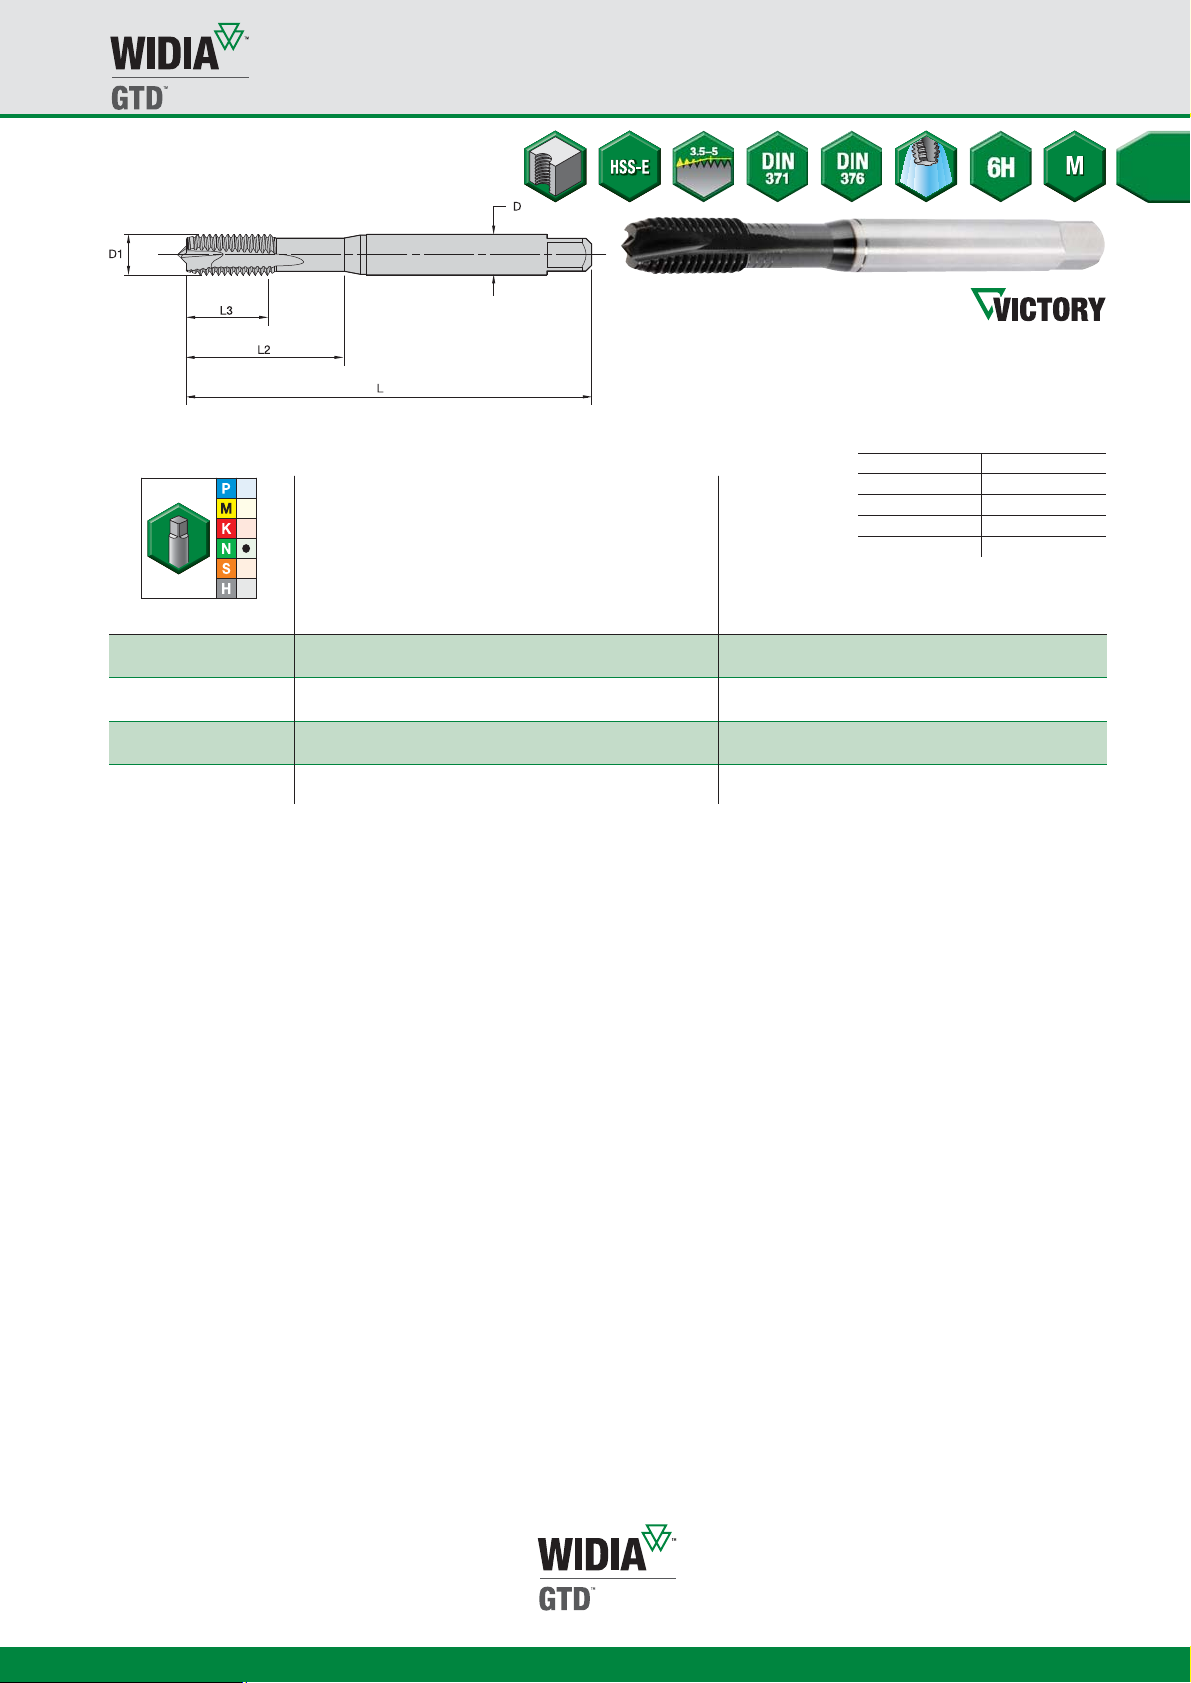
• WN48EG DLC for aluminum.
High-Performance Taps
Victory™Spiral-Point Plug HSS-E-PM Taps • Through Holes
䢇
first choice
嘷
alternate choice
GT70 • Form B Plug Chamfer • Metric DIN 371 and 376
WN48EG D1 size L L3 L2 D
GT705001 M3 X 0,5 56 11 18 3,5 2 DIN 371 6H
GT705002 M4 X 0,7 63 13 21 4,5 2 DIN 371 6H
GT705003 M5 X 0,8 70 15 25 6,0 2 DIN 371 6H
GT705004 M6 X 1 80 17 30 6,0 2 DIN 371 6H
GT705005 M8 X 1,25 90 20 35 8,0 2 DIN 371 6H
GT705006 M10 X 1,5 100 22 39 10,0 2 DIN 371 6H
GT705007 M12 X 1,75 110 24 — 9,0 3 DIN 376 6H
GT705008 M16 X 2 110 27 — 12,0 3 DIN 376 6H
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A41
Page 41
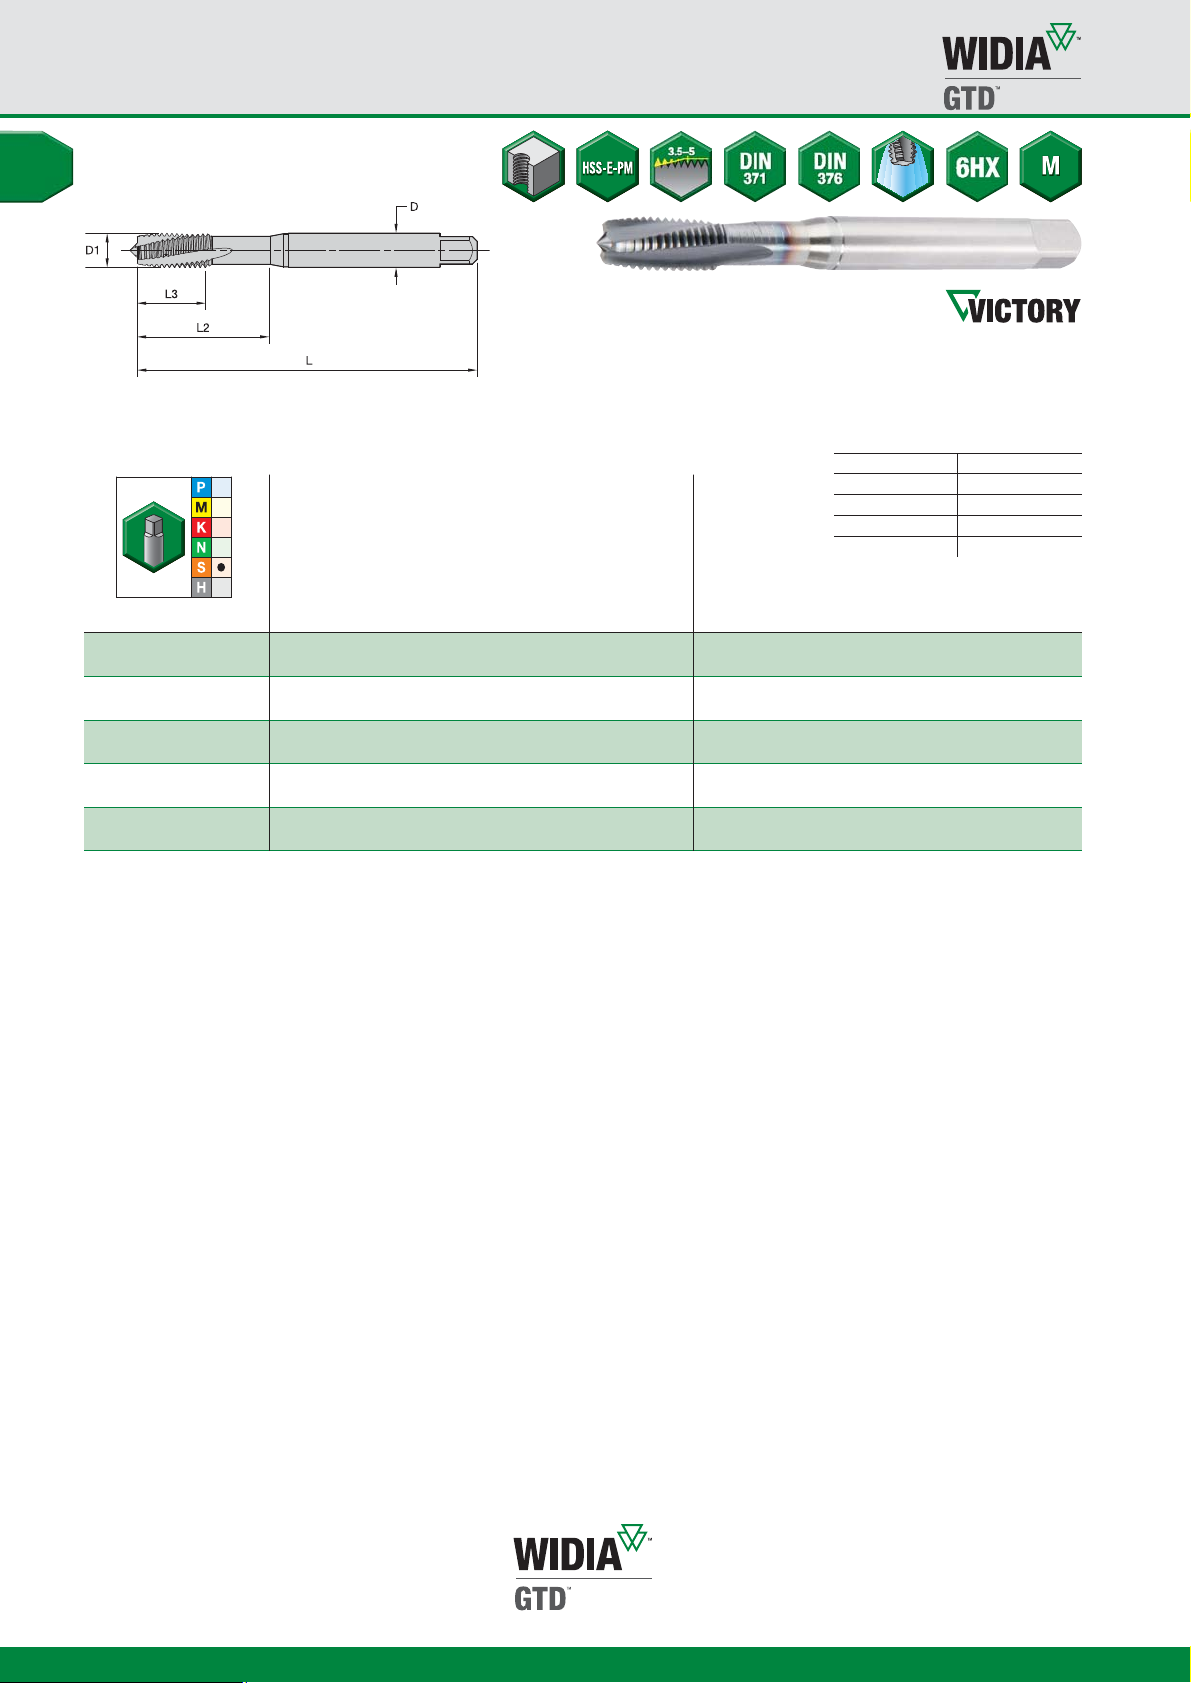
High-Performance Taps
Victory™Left-Hand Spiral-Flute HSS-E-PM Taps • Through Holes
• WS32MG TiCN for nickel and
nickel alloys.
䢇
first choice
嘷
alternate choice
Holemaking • High-Performance Taps
GT10 • Form D Plug Chamfer • Metric DIN 371 and 376
WS32MG D1 size L L3 L2 D
GT105001 M3 X 0,5 56 11 18 3,5 2 DIN 371 6HX
GT105002 M4 X 0,7 63 13 21 4,5 3 DIN 371 6HX
GT105003 M5 X 0,8 70 15 25 6,0 3 DIN 371 6HX
GT105004 M6 X 1 80 17 30 6,0 3 DIN 371 6HX
GT105005 M8 X 1,25 90 20 35 8,0 3 DIN 371 6HX
GT105006 M10 X 1,5 100 22 39 10,0 3 DIN 371 6HX
GT105007 M12 X 1,75 110 24 — 9,0 3 DIN 376 6HX
GT105008 M14 X 2 110 26 — 11,0 3 DIN 376 6HX
GT105009 M16 X 2 110 27 — 12,0 3 DIN 376 6HX
GT105010 M20 X 2,5 140 32 — 16,0 3 DIN 376 6HX
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
A42
WWW.WIDIA.COM
Page 42
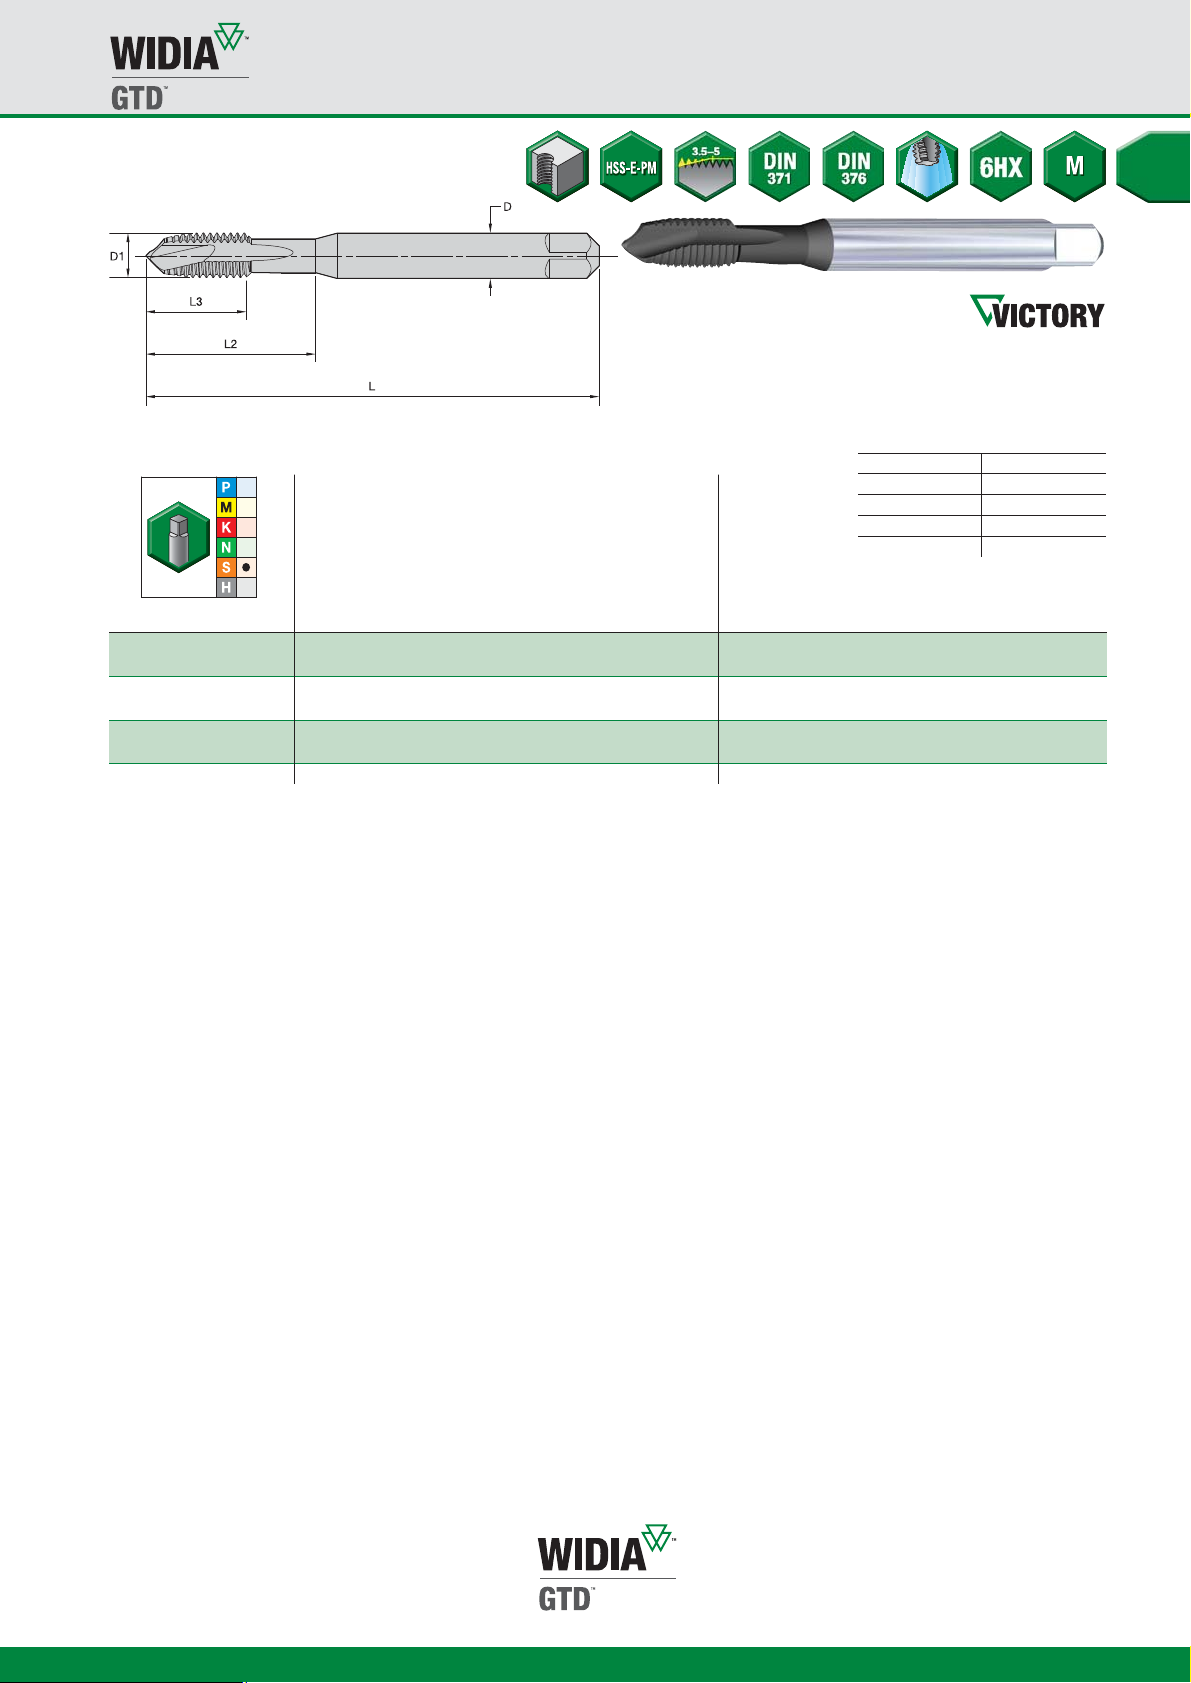
• WN35MG TiN/DLC for titanium and
titanium alloys.
High-Performance Taps
Victory™Spiral-Point Plug HSS-E-PM Taps • Through Holes
䢇
first choice
嘷
alternate choice
GT14 • Form B Plug Chamfer • Metric DIN 371 and 376
WN35MG D1 size L L3 L2 D
GT145001 M3 X 0,5 56 11 18 3,5 3 DIN 371 6HX
GT145002 M4 X 0,7 63 13 21 4,5 3 DIN 371 6HX
GT145003 M5 X 0,8 70 15 25 6,0 3 DIN 371 6HX
GT145004 M6 X 1 80 17 30 6,0 3 DIN 371 6HX
GT145005 M8 X 1,25 90 20 35 8,0 3 DIN 371 6HX
GT145006 M10 X 1,5 100 22 39 10,0 3 DIN 371 6HX
GT145007 M12 X 1,75 110 24 — 9,0 3 DIN 376 6HX
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A43
Page 43
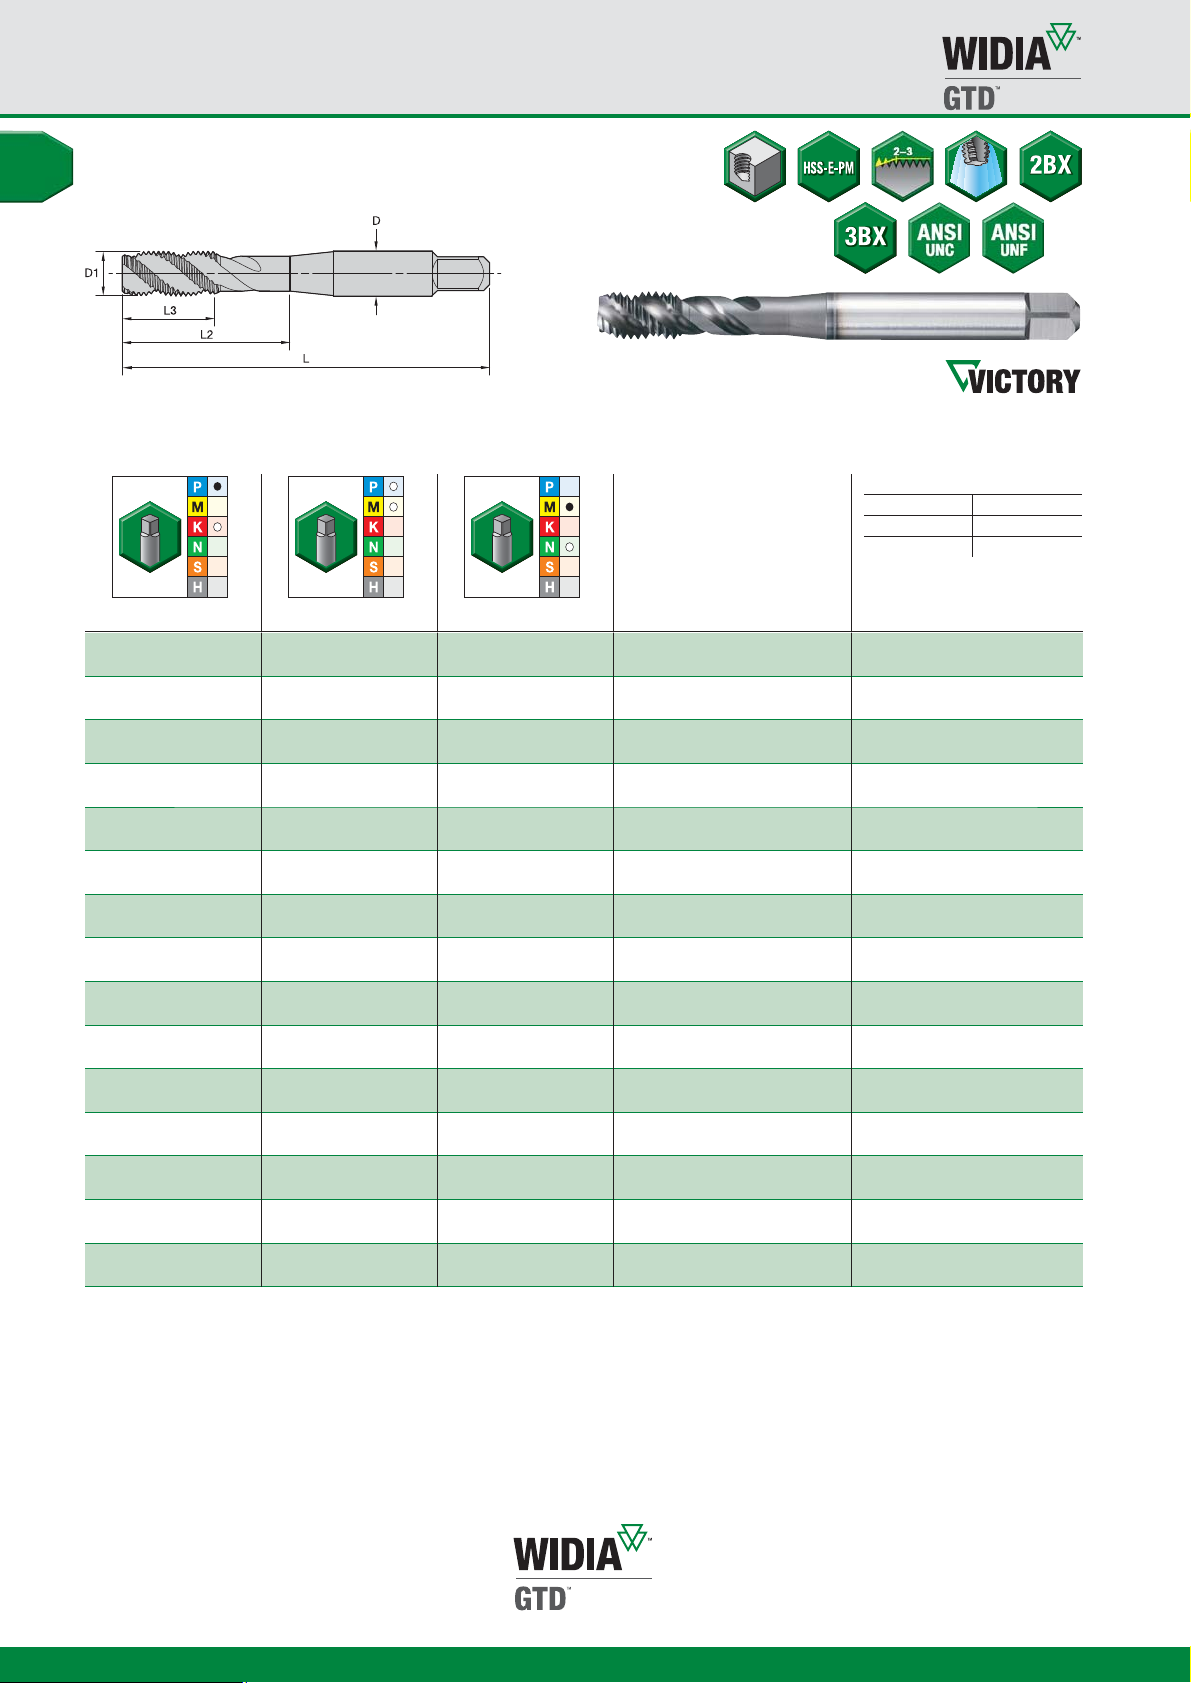
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GM6515 TiN + CrC/C for stainless steel.
• GP6520 TiCN for steel.
• GP6505 Oxide for steel.
GT30 • Machine Screw and Fractional • Form C Semi-Bottoming Chamfer
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Fractional D Inch
.250–.375 +0, -.0004
.438–.625 +0, -.0004
GP6520 GP6505 GM6515 D1 size L L3 L2 D
GT305031 — GT305001 2 - 56 1.75 .44 .49 .141 2 3BX
GT305032 — GT305002 4 - 40 1.88 .56 .68 .141 2 2BX
GT305033 GT305125 GT305003 4 - 40 1.88 .56 .68 .141 2 3BX
GT305034 — GT305004 6 - 32 1.99 .36 .71 .141 3 2BX
GT305035 GT305126 GT305005 6 - 32 1.99 .36 .71 .141 3 3BX
GT305036 GT305127 GT305006 8 - 32 2.12 .31 .76 .168 3 3BX
GT305037 GT305128 GT305007 10 - 24 2.37 .47 .91 .194 3 3BX
GT305052 — GT305022 10 - 32 2.36 .47 .91 .194 3 2BX
GT305053 GT305140 GT305023 10 - 32 2.36 .47 .91 .194 3 3BX
GT305038 GT305129 GT305008 1/4 - 20 2.50 .44 1.01 .255 3 2BX
GT305039 GT305130 GT305009 1/4 - 20 2.50 .44 1.01 .255 3 3BX
GT305054 GT305141 GT305024 1/4 - 28 2.49 .43 1.00 .255 3 2BX
GT305055 GT305142 GT305025 1/4 - 28 2.49 .43 1.00 .255 3 3BX
GT305040 GT305131 GT305010 5/16 - 18 2.72 .49 1.13 .318 3 2BX
GT305041 GT305132 GT305011 5/16 - 18 2.72 .49 1.13 .318 3 3BX
GT305056 GT305143 GT305026 5/16 - 24 2.71 .48 1.13 .318 3 2BX
GT305057 — GT305027 5/16 - 24 2.71 .48 1.13 .318 3 3BX
GT305042 GT305133 GT305012 3/8 - 16 2.94 .60 1.27 .381 3 2BX
GT305043 GT305134 GT305013 3/8 - 16 2.94 .60 1.27 .381 3 3BX
GT305058 — GT305028 3/8 - 24 2.92 .58 1.25 .381 3 3BX
GT305044 GT305135 GT305014 7/16 - 14 3.16 .71 1.49 .323 4 3BX
GT305059 GT305145 GT305029 7/16 - 20 3.16 .71 1.49 .323 4 3BX
GT305045 GT305136 GT305015 1/2 - 13 3.38 .77 1.74 .367 4 2BX
GT305046 GT305137 GT305016 1/2 - 13 3.38 .77 1.74 .367 4 3BX
GT305060 GT305147 GT305030 1/2 - 20 3.38 .77 1.74 .367 4 3BX
GT305047 — GT305017 5/8 - 11 3.81 .91 1.89 .480 4 2BX
GT305048 GT305138 GT305018 5/8 - 11 3.81 .91 1.89 .480 4 3BX
GT305049 — GT305019 3/4 - 10 4.25 1.00 2.08 .590 4 2BX
GT305050 GT305139 GT305020 3/4 - 10 4.25 1.00 2.08 .590 4 3BX
GT305051 — GT305021 1 - 8 5.13 1.25 2.58 .800 4 3BX
number
of flutes
class
of fit
A44
WWW.WIDIA.COM
Page 44
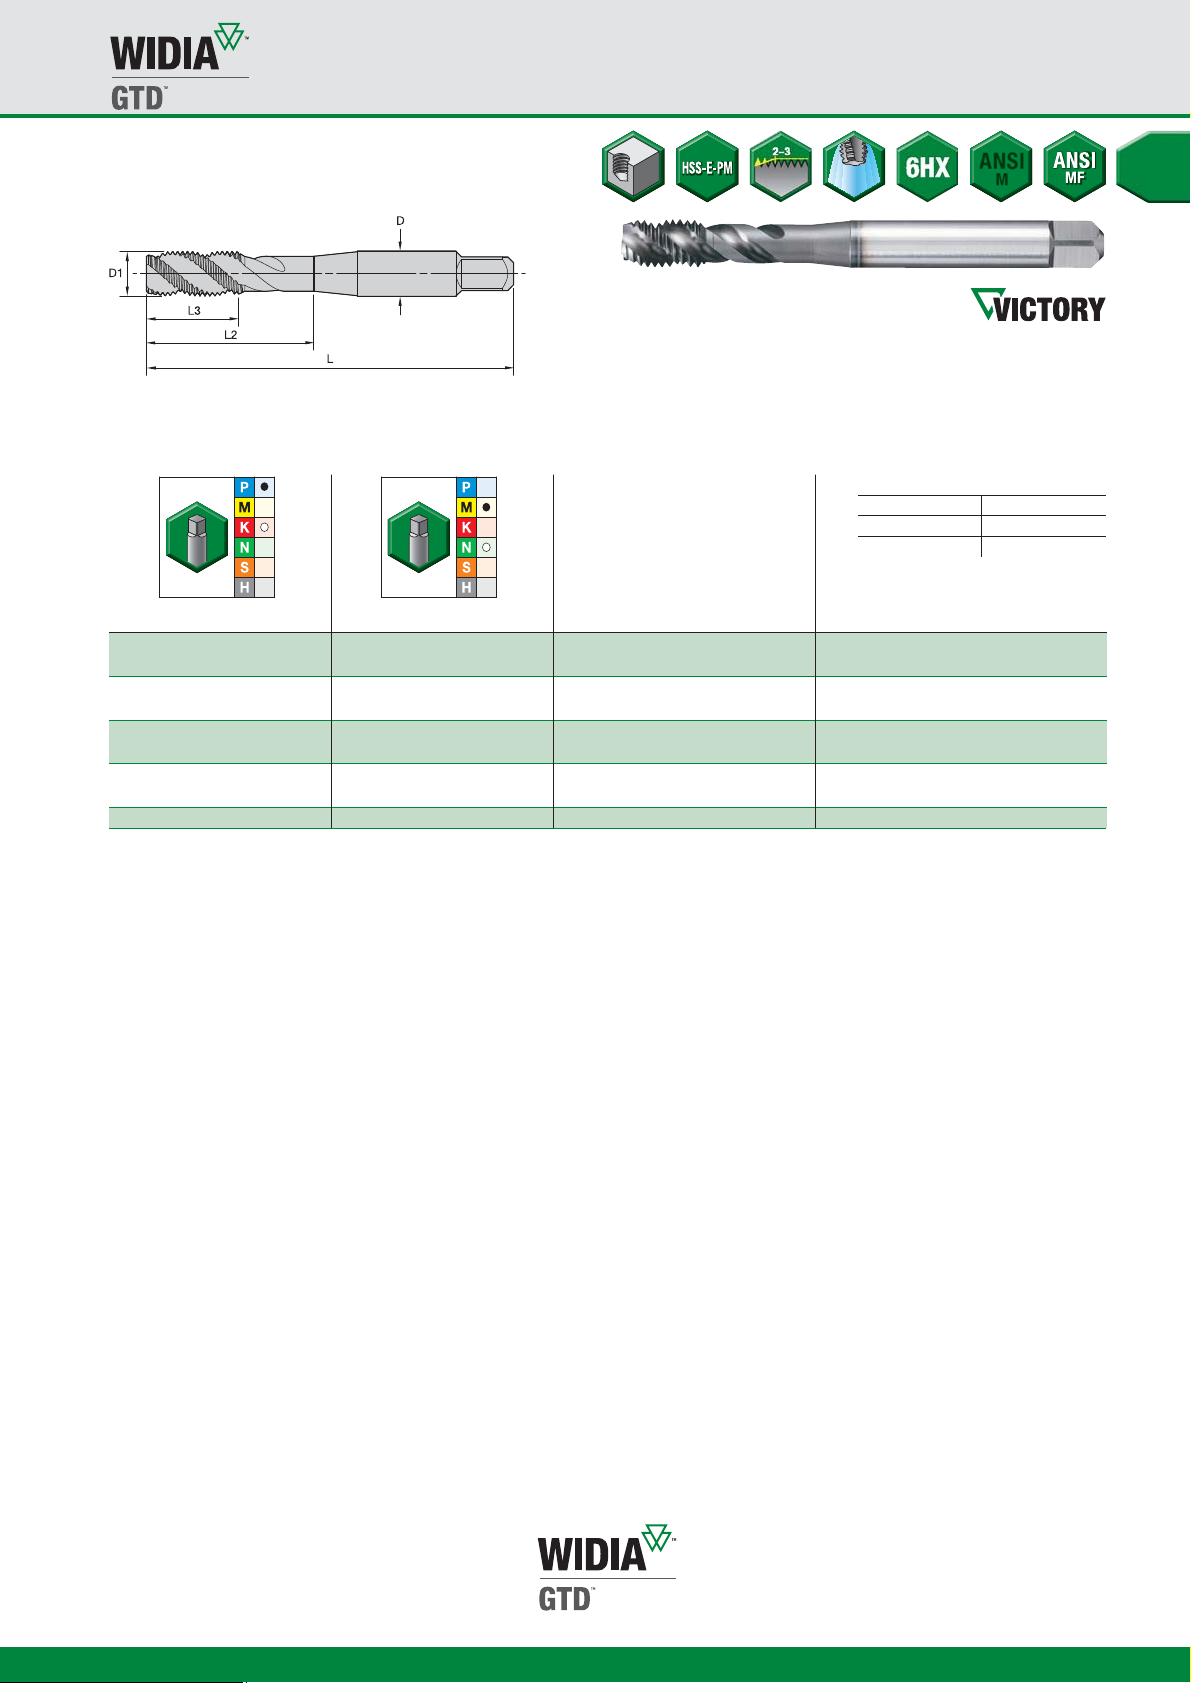
• GM6515 TiN + CrC/C for stainless steel.
• GP6520 TiCN for steel.
GT30 • Form C Semi-Bottoming Chamfer • Metric ANSI
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
ANSI
M
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Fractional D Inch
.250–.375 +0, -.0004
.438–.625 +0, -.0004
Holemaking • High-Performance Taps
GP6520 GM6515 D1 size L L3 L2 D
GT305070 GT305061 M3 X 0,5 1.94 .63 .75 .141 3 6HX
GT305071 GT305062 M4 X 0,7 2.13 .32 .76 .168 3 6HX
GT305072 GT305063 M5 X 0,8 2.38 .47 .91 .194 3 6HX
GT305073 GT305064 M6 X 1 2.50 .46 1.01 .255 3 6HX
GT305074 GT305065 M8 X 1,25 2.72 .48 1.12 .318 3 6HX
GT305075 GT305066 M10 X 1,5 2.94 .53 1.26 .381 3 6HX
GT305076 GT305067 M12 X 1,75 3.38 .77 1.74 .367 4 6HX
GT305077 GT305068 M14 X 2 3.59 .83 1.74 .429 4 6HX
GT305078 GT305069 M16 X 2 3.81 .91 1.89 .480 4 6HX
number
of flutes
class
of fit
WWW.WIDIA.COM
A45
Page 45
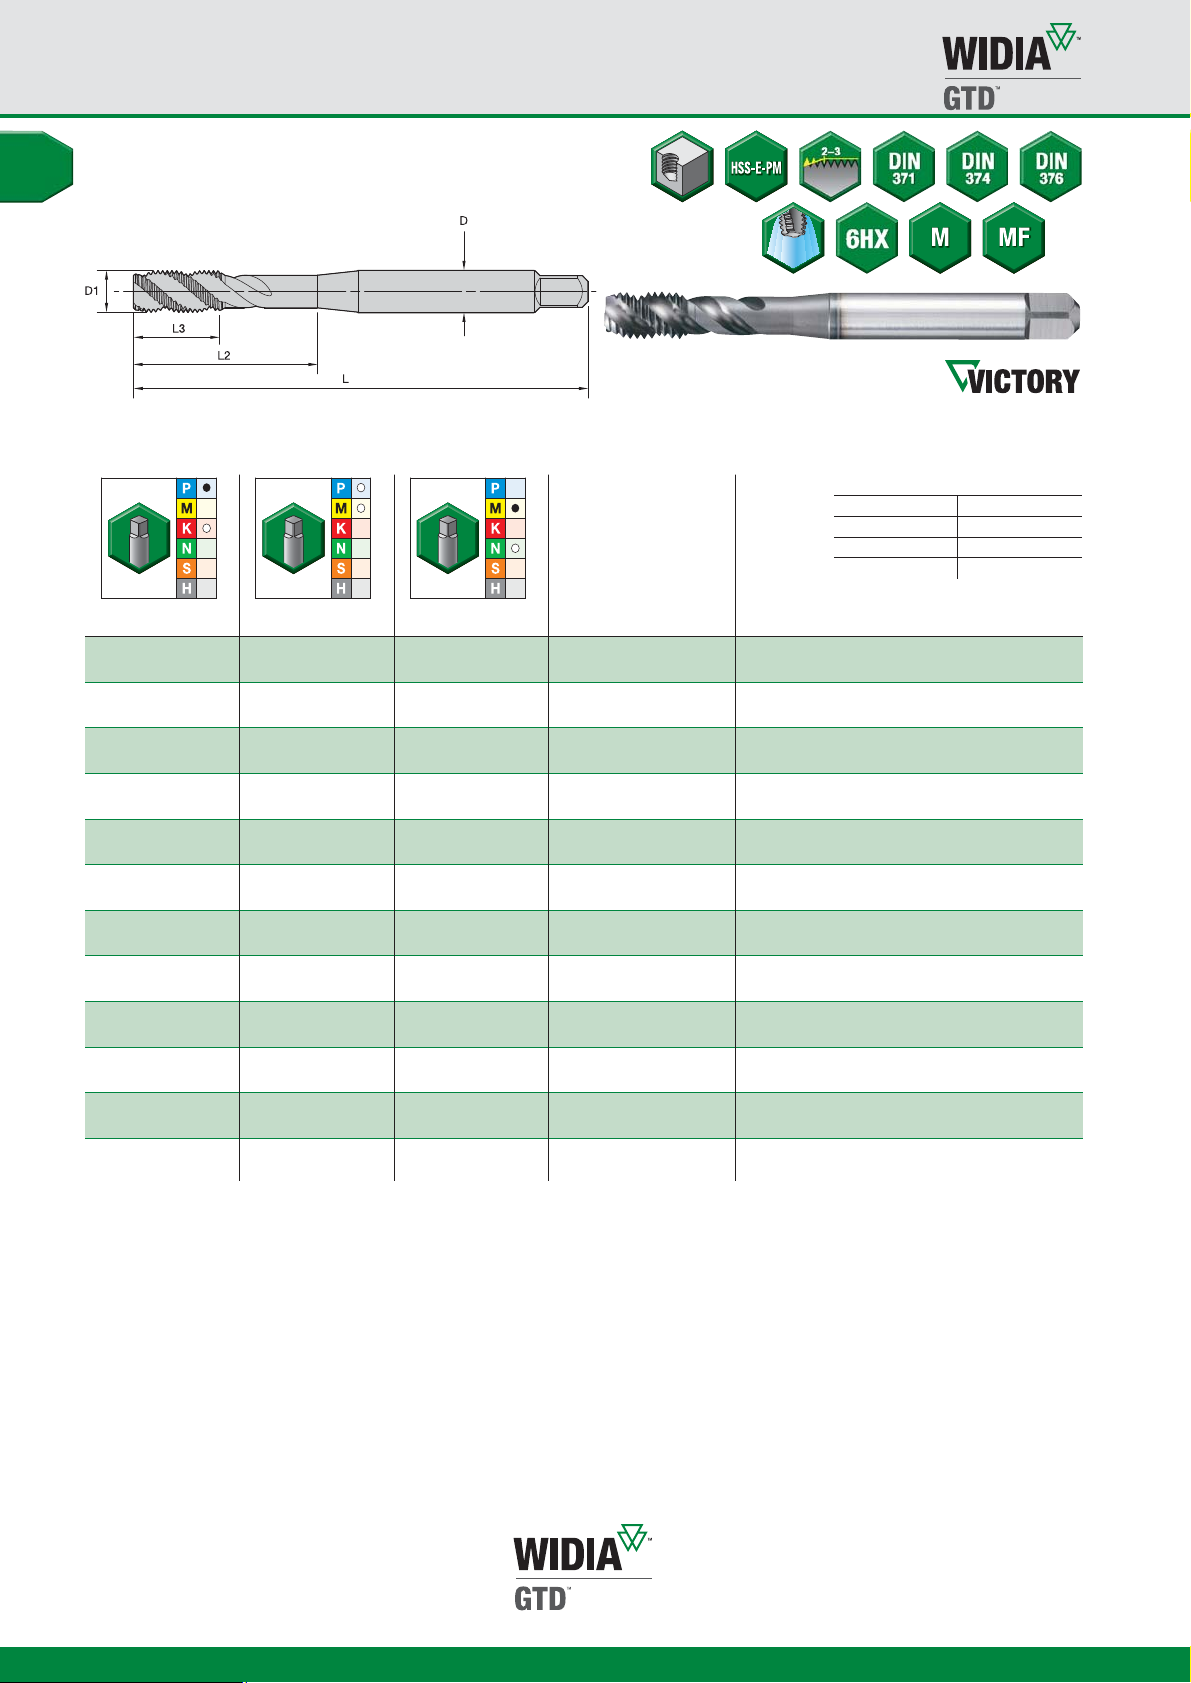
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GM6515 TiN + CrC/C for stainless steel.
• GP6520 TiCN for steel.
• GP6505 oxide for steel.
GT30 • Form C Semi-Bottoming Chamfer • Metric DIN 371, 374, and 376
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
GP6520 GP6505 GM6515 D1 size L L3 L2 D
GT305097 GT305116 GT305148 M3 X 0,5 56 8 18 3,5 3 DIN 371 6HX
GT305098 GT305117 GT305079 M4 X 0,7 63 10 21 4,5 3 DIN 371 6HX
GT305099 GT305118 GT305080 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT305100 GT305119 GT305081 M6 X 1 80 10 30 6,0 3 DIN 371 6HX
GT305109 — GT305090 M8 X 1 90 13 35 6,0 4 DIN 374 6HX
GT305101 GT305120 GT305082 M8 X 1,25 90 13 35 8,0 3 DIN 371 6HX
GT305110 — GT305091 M10 X 1 90 10 35 7,0 4 DIN 374 6HX
GT305111 — GT305092 M10 X 1,25 100 15 39 7,0 4 DIN 374 6HX
GT305102 GT305121 GT305083 M10 X 1,5 100 15 39 10,0 3 DIN 371 6HX
GT305112 — GT305093 M12 X 1,5 100 15 39 9,0 4 DIN 374 6HX
GT305103 GT305122 GT305084 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT305113 — GT305094 M14 X 1,5 100 15 47 11,0 4 DIN 374 6HX
GT305104 GT305123 GT305085 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT305114 — GT305095 M16 X 1,5 100 15 46 12,0 4 DIN 374 6HX
GT305105 GT305124 GT305086 M16 X 2 110 20 51 12,0 4 DIN 376 6HX
GT305115 — GT305096 M18 X 1,5 110 15 50 14,0 4 DIN 374 6HX
GT305106 — GT305087 M18 X 2,5 125 25 58 14,0 4 DIN 376 6HX
GT305107 — GT305088 M22 X 2,5 140 25 70 18,0 4 DIN 376 6HX
GT305108 — GT305089 M24 X 3 160 30 77 18,0 4 DIN 376 6HX
GT305161 — — M24 X 3 160 30 77 18,0 5 DIN 376 6HX
GT305163 — — M30 X 3,5 180 35 91 22,0 5 DIN 376 6HX
GT305164 — — M33 X 3,5 180 35 100 25,0 5 DIN 376 6HX
GT305166 — — M36 X 4 200 40 110 28,0 5 DIN 376 6HX
GT305168 — — M42 X 4,5 200 45 120 32,0 5 DIN 376 6HX
number
of flutes
dimension
standard
class
of fit
A46
WWW.WIDIA.COM
Page 46
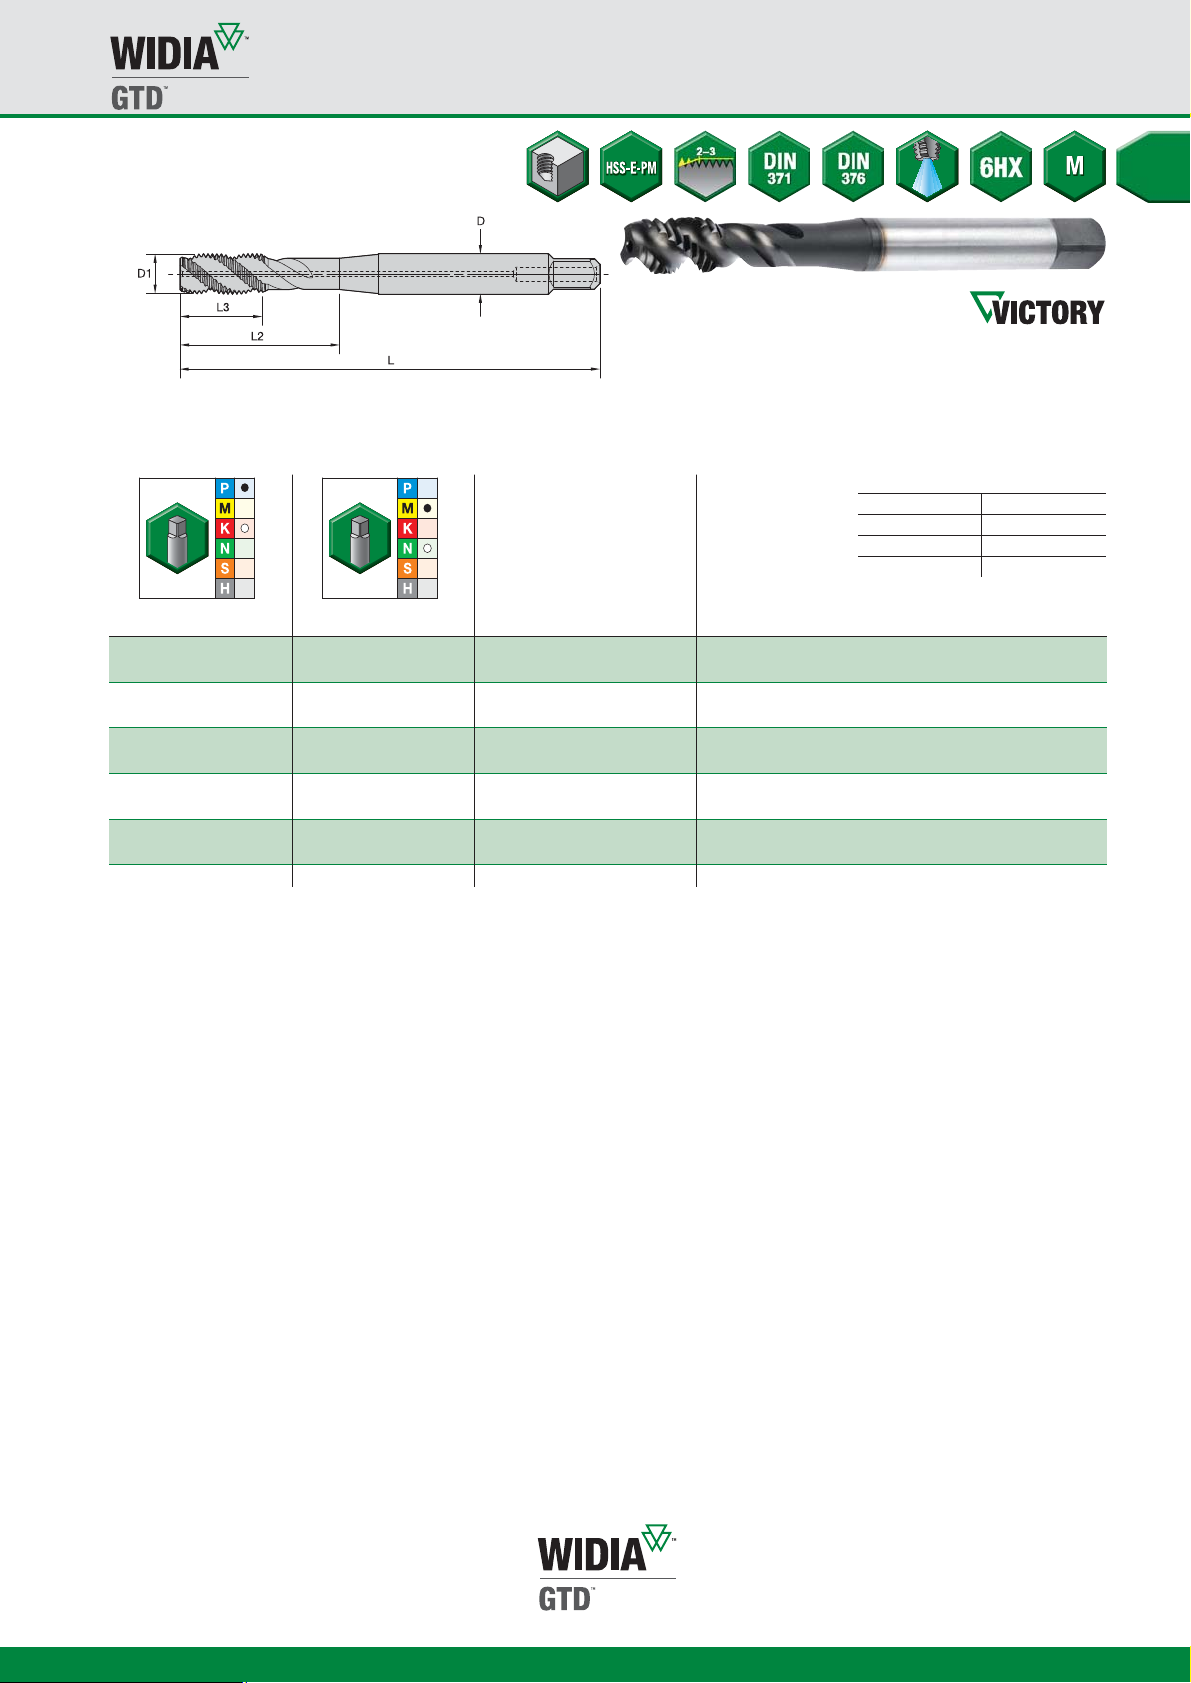
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GM6515 TiN + CrC/C for
stainless steel.
• GP6520 TiCN for steel.
䢇
first choice
嘷
alternate choice
GT31 • Form C Semi-Bottoming Chamfer • Through Coolant • Metric DIN 371 and 376
12–16 +0, -0,011
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
Holemaking • High-Performance Taps
GP6520 GM6515 D1 size L L3 L2 D
GT315007 GT315001 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT315008 GT315002 M6 X 1 80 10 30 6,0 3 DIN 371 6HX
GT315009 GT315003 M8 X 1,25 90 13 35 8,0 3 DIN 371 6HX
GT315010 GT315004 M10 X 1,5 100 15 39 10,0 3 DIN 371 6HX
GT315011 GT315005 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT315012 GT315006 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT315025 — M24 X 3 160 30 77 18,0 5 DIN 376 6HX
GT315027 — M30 X 3,5 180 35 91 22,0 5 DIN 376 6HX
GT315028 — M33 X 3,5 180 35 100 25,0 5 DIN 376 6HX
GT315030 — M36 X 4 200 40 110 28,0 5 DIN 376 6HX
GT315032 — M42 X 4,5 200 45 120 32,0 5 DIN 376 6HX
number
of flutes
dimension
standard
class
of fit
WWW.WIDIA.COM
A47
Page 47
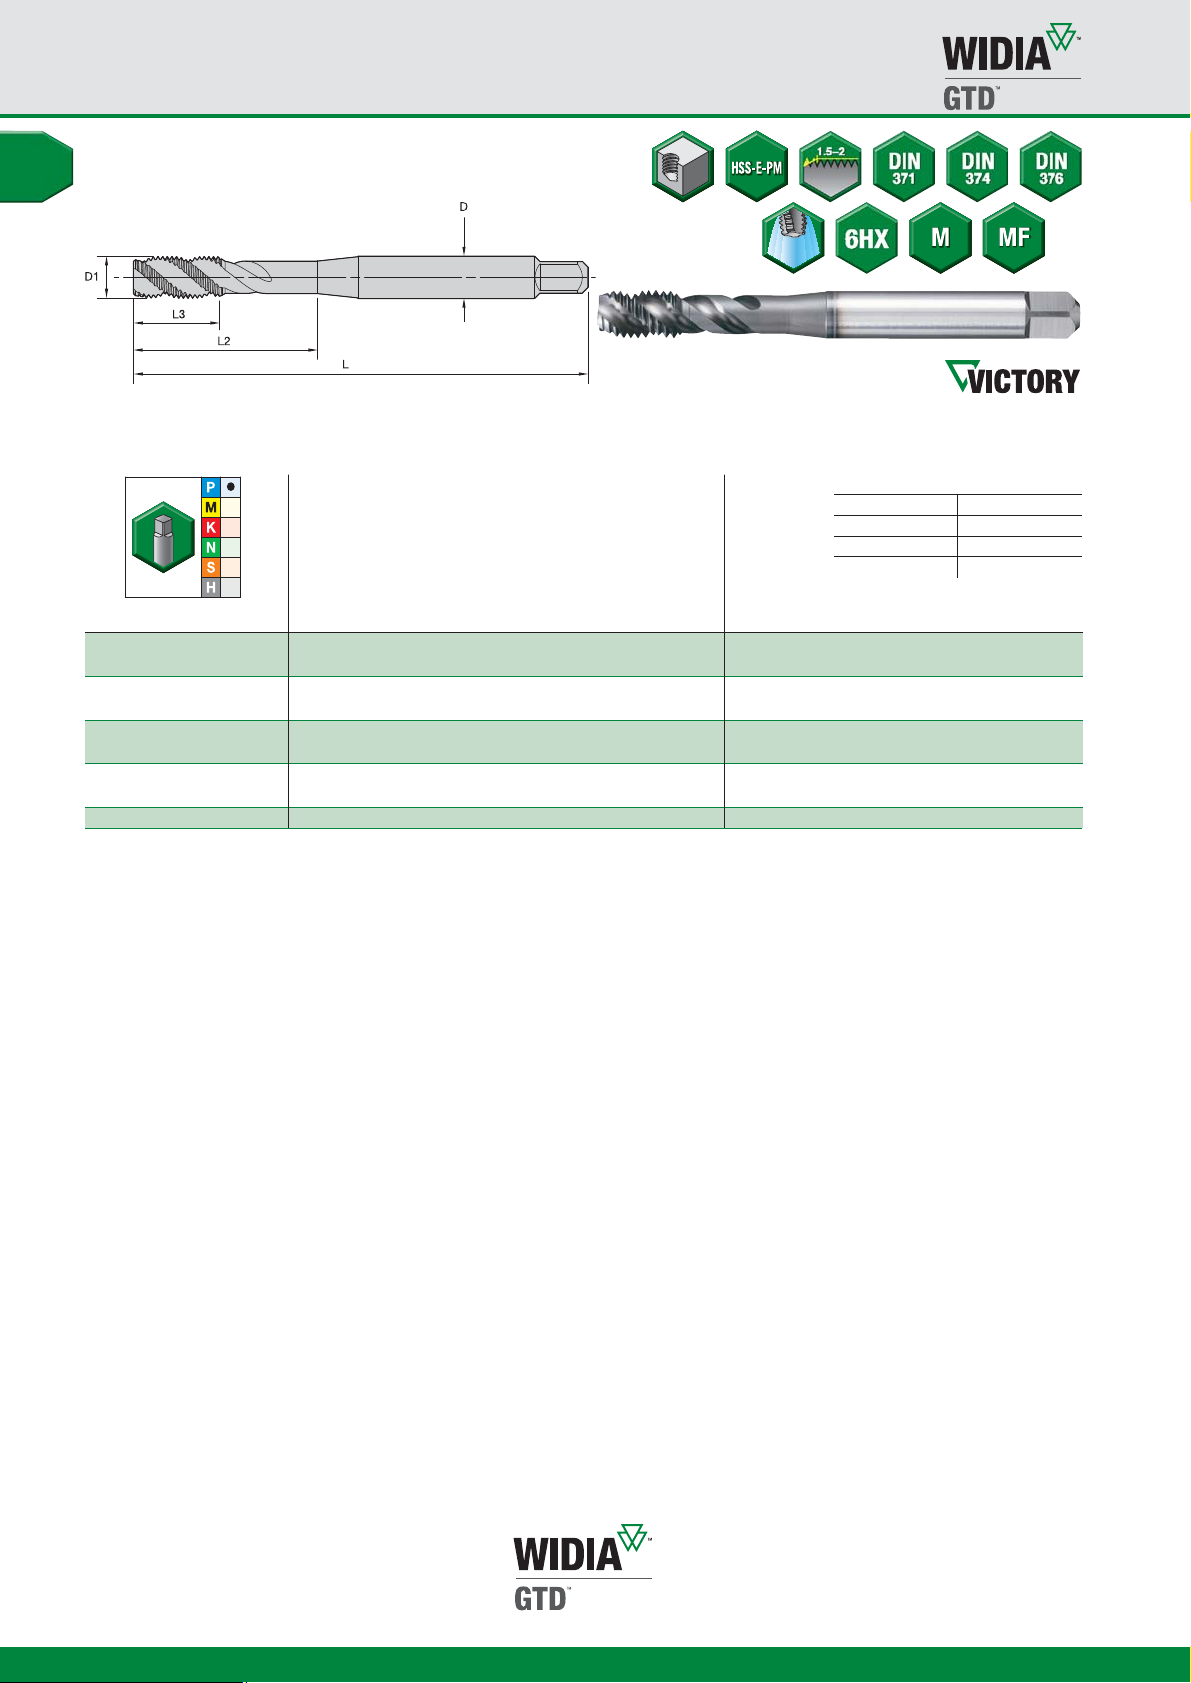
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Threading Close to the Bottom in a Blind Hole
GT32 • Form E Bottoming Chamfer • Metric DIN 371, 374, and 376
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
GP6520 D1 size L L3 L2 D
GT325001 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT325002 M6 X 1 80 10 30 6,0 3 DIN 371 6HX
GT325003 M8 X 1,25 90 13 35 8,0 3 DIN 371 6HX
GT325004 M10 X 1,5 100 15 39 10,0 3 DIN 371 6HX
GT325007 M12 X 1,5 100 15 39 9,0 4 DIN 374 6HX
GT325005 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT325008 M14 X 1,5 100 15 47 11,0 4 DIN 374 6HX
GT325006 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT325009 M16 X 1,5 100 15 46 12,0 4 DIN 374 6HX
number
of flutes
dimension
standard
class
of fit
A48
WWW.WIDIA.COM
Page 48
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Threading Close to the Bottom in a Blind Hole
䢇
first choice
嘷
alternate choice
GT33 • Form E Bottoming Chamfer • Through Coolant • Metric DIN 371, 374, and 376
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT335001 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT335002 M6 X 1 80 10 30 6,0 3 DIN 371 6HX
GT335003 M8 X 1,25 90 13 35 8,0 3 DIN 371 6HX
GT335004 M10 X 1,5 100 15 39 10,0 3 DIN 371 6HX
GT335007 M12 X 1,5 100 15 39 9,0 4 DIN 374 6HX
GT335005 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT335008 M14 X 1,5 100 15 47 11,0 4 DIN 374 6HX
GT335006 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT335009 M16 X 1,5 100 15 46 12,0 4 DIN 374 6HX
number
of flutes
dimension
standard
class
of fit
WWW.WIDIA.COM
A49
Page 49
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• WP31MG TiN for steel 32–44 HRC.
䢇
first choice
嘷
alternate choice
Holemaking • High-Performance Taps
GT02 • Form C Semi-Bottoming Chamfer • Metric DIN 371, 374, and 376
WP31MG D1 size L L3 L2 D
GT025001 M3 X 0,5 56 11 18 3,5 3 DIN 371 6H
GT025002 M4 X 0,7 63 13 21 4,5 3 DIN 371 6H
GT025003 M5 X 0,8 70 15 25 6,0 3 DIN 371 6H
GT025004 M6 X 1 80 17 30 6,0 3 DIN 371 6H
GT025012 M8 X 1 90 17 — 6,0 3 DIN 374 6H
GT025005 M8 X 1,25 90 20 35 8,0 3 DIN 371 6H
GT025013 M10 X 1 90 18 — 7,0 3 DIN 374 6H
GT025014 M10 X 1,25 100 22 — 7,0 3 DIN 374 6H
GT025006 M10 X 1,5 100 22 39 10,0 3 DIN 371 6H
GT025015 M12 X 1,25 100 22 — 9,0 3 DIN 374 6H
GT025016 M12 X 1,5 100 22 — 9,0 3 DIN 374 6H
GT025007 M12 X 1,75 110 24 44 12,0 3 DIN 376 6H
GT025017 M14 X 1,5 100 22 — 11,0 3 DIN 374 6H
GT025008 M14 X 2 110 26 52 11,0 3 DIN 376 6H
GT025018 M16 X 1,5 100 22 — 12,0 3 DIN 374 6H
GT025009 M16 X 2 110 27 — 12,0 3 DIN 376 6H
GT025010 M18 X 2 125 30 — 14,0 4 DIN 376 6H
GT025011 M20 X 2,5 140 32 — 16,0 4 DIN 376 6H
number
of flutes
Shank Tolerance
D Tolerance h9
1-3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
A50
WWW.WIDIA.COM
Page 50
• WN48EG DLC for aluminum.
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
䢇
first choice
嘷
alternate choice
GT80 • Form C Semi-Bottoming Chamfer • Metric DIN 371 and 376
WN48EG D1 size L L3 L2 D
GT805001 M3 X 0,5 56 6 18 3,5 2 DIN 371 6H
GT805002 M4 X 0,7 63 7 21 4,5 2 DIN 371 6H
GT805003 M5 X 0,8 70 8 25 6,0 2 DIN 371 6H
GT805004 M6 X 1 80 10 30 6,0 2 DIN 371 6H
GT805005 M8 X 1,25 90 14 35 8,0 2 DIN 371 6H
GT805006 M10 X 1,5 100 16 39 10,0 2 DIN 371 6H
GT805007 M12 X 1,75 110 18 — 9,0 3 DIN 376 6H
GT805008 M16 X 2 110 22 — 12,0 3 DIN 376 6H
GT805009 M20 X 2,5 140 25 — 16,0 3 DIN 376 6H
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A51
Page 51
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Hole 3 x D
• WH36MG TiAlN/MoS2for steel
32–44 HRC (3 x D).
䢇
first choice
嘷
alternate choice
Holemaking • High-Performance Taps
GT04 • Form C Semi-Bottoming Chamfer • Metric DIN 371, 374, and 376
WH36MG D1 size L L3 L2 D
GT045001 M3 X 0,5 56 6 18 3,5 3 DIN 371 6H
GT045002 M4 X 0,7 63 7 21 4,5 3 DIN 371 6H
GT045003 M5 X 0,8 70 8 25 6,0 3 DIN 371 6H
GT045004 M6 X 1 80 10 30 6,0 3 DIN 371 6H
GT045012 M8 X 1 90 10 — 6,0 3 DIN 374 6H
GT045005 M8 X 1,25 90 14 35 8,0 3 DIN 371 6H
GT045013 M10 X 1 90 10 — 7,0 3 DIN 374 6H
GT045014 M10 X 1,25 100 16 — 7,0 3 DIN 374 6H
GT045006 M10 X 1,5 100 16 39 10,0 3 DIN 371 6H
GT045015 M12 X 1,25 100 15 — 9,0 4 DIN 374 6H
GT045016 M12 X 1,5 100 15 — 9,0 4 DIN 374 6H
GT045007 M12 X 1,75 110 18 — 9,0 4 DIN 376 6H
GT045017 M14 X 1,5 100 15 — 11,0 4 DIN 374 6H
GT045008 M14 X 2 110 20 — 11,0 4 DIN 376 6H
GT045018 M16 X 1,5 100 15 — 12,0 4 DIN 374 6H
GT045009 M16 X 2 110 22 — 12,0 4 DIN 376 6H
GT045010 M18 X 2 125 25 — 14,0 4 DIN 376 6H
GT045011 M20 X 2,5 140 25 — 16,0 4 DIN 376 6H
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
A52
WWW.WIDIA.COM
Page 52
• WS32MG TiCN for steel 44–55 HRC.
High-Performance Taps
Victory™Straight-Flute HSS-E-PM Taps • Blind and Through Holes
䢇
first choice
嘷
alternate choice
GT06 • Form C Semi-Bottoming Chamfer • Metric DIN 371, 374, and 376
WS32MG D1 size L L3 L2 D
GT065003 M6 X 1 80 10 30 6,0 4 DIN 371 6HX
GT065006 M8 X 1 90 10 35 8,0 5 DIN 374 6HX
GT065001 M8 X 1,25 90 14 35 8,0 5 DIN 371 6HX
GT065008 M12 X 1,5 100 15 — 9,0 5 DIN 374 6HX
GT065004 M12 X 1,75 110 18 — 9,0 5 DIN 376 6HX
GT065007 M10 X 1 90 10 35 10,0 5 DIN 374 6HX
GT065002 M10 X 1,5 100 16 39 10,0 5 DIN 371 6HX
GT065009 M14 X 1,5 100 15 — 11,0 6 DIN 374 6HX
GT065010 M16 X 1,5 100 15 — 12,0 6 DIN 374 6HX
GT065005 M16 X 2 110 22 — 12,0 6 DIN 376 6HX
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A53
Page 53
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holess
• WS32MG TiCN for nickel and
nickel alloys.
䢇
first choice
嘷
alternate choice
Holemaking • High-Performance Taps
GT12 • Form C Semi-Bottoming Chamfer • Metric DIN 371 and 376
WS32MG D1 size L L3 L2 D
GT125001 M3 X 0,5 56 11 18 3,5 2 DIN 371 6HX
GT125002 M4 X 0,7 63 13 21 4,5 3 DIN 371 6HX
GT125003 M5 X 0,8 70 15 25 6,0 3 DIN 371 6HX
GT125004 M6 X 1 80 17 30 6,0 3 DIN 371 6HX
GT125005 M8 X 1,25 90 20 35 8,0 3 DIN 371 6HX
GT125006 M10 X 1,5 100 22 39 10,0 3 DIN 371 6HX
GT125007 M12 X 1,75 110 24 — 9,0 3 DIN 376 6HX
GT125008 M14 X 2 110 26 — 11,0 3 DIN 376 6HX
GT125009 M16 X 2 110 27 — 12,0 3 DIN 376 6HX
GT125010 M20 X 2,5 140 32 — 16,0 3 DIN 376 6HX
number
of flutes
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
dimension
standard
class
of fit
A54
WWW.WIDIA.COM
Page 54
• WN35MG TiN/DLC for titanium and
titanium alloys.
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
䢇
first choice
嘷
alternate choice
GT16 • Form C Semi-Bottoming Chamfer • Metric DIN 371
WN35MG D1 size L L3 L2 D
GT165001 M3 X 0,5 56 6 18 3,5 3 6HX
GT165002 M4 X 0,7 63 7 21 4,5 3 6HX
GT165003 M5 X 0,8 70 8 25 6,0 3 6HX
GT165004 M6 X 1 80 10 30 6,0 3 6HX
GT165005 M8 X 1,25 90 14 35 8,0 3 6HX
GT165006 M10 X 1,5 100 16 39 10,0 3 6HX
GT165007 M12 X 1,75 110 18 44 12,0 3 6HX
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
number
of flutes
class
of fit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A55
Page 55
High-Performance Taps
Victory™Straight-Flute HSS-E-PM Taps • Through and Blind Holes
• GP6520 TiCN for cast iron and cast aluminum.
GT40 • Machine Screw and Fractional • Form C Semi-Bottoming Chamfer
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT405012 10 - 24 2.37 .47 .91 .194 4 3BX
GT405013 10 - 32 2.36 .47 .91 .194 4 3BX
GT405014 1/4 - 20 2.50 .44 1.01 .255 4 2BX
GT405015 1/4 - 20 2.50 .44 1.01 .255 4 3BX
GT405016 1/4 - 28 2.49 .43 1.00 .255 4 2BX
GT405017 1/4 - 28 2.49 .43 1.00 .255 4 3BX
GT405018 5/16 - 18 2.72 .49 1.13 .318 4 2BX
GT405019 5/16 - 18 2.72 .49 1.13 .318 4 3BX
GT405020 5/16 - 24 2.71 .48 1.13 .318 4 3BX
GT405021 3/8 - 16 2.94 .60 1.27 .381 4 2BX
GT405022 3/8 - 16 2.94 .60 1.27 .381 4 3BX
GT405023 3/8 - 24 2.92 .58 1.25 .381 4 3BX
GT405024 7/16 - 14 3.16 .71 1.49 .323 4 3BX
GT405025 7/16 - 20 3.16 .71 1.49 .323 4 3BX
GT405026 1/2 - 13 3.38 .77 1.74 .367 4 3BX
GT405027 1/2 - 20 3.38 .77 1.74 .367 4 3BX
GT405028 5/8 - 11 3.81 .91 1.89 .480 4 3BX
GT405029 3/4 - 10 4.25 1.00 2.08 .590 4 3BX
䢇
first choice
嘷
alternate choice
number
of flutes
Shank Tolerance
D Fractional D Inch
.250–.375 +0, -.0004
.438–.625 +0, -.0004
class
of fit
A56
WWW.WIDIA.COM
Page 56
Victory™Straight-Flute HSS-E-PM Taps • Through and Blind Holes
• GP6520 TiCN for cast iron and cast aluminum.
GT40 • Form C Semi-Bottoming Chamfer • Metric ANSI
GP6520 D1 size L L3 L2 D
GT405030 M3 X 0,5 1.94 .63 .75 .140 4 6HX
GT405031 M4 X 0,7 2.12 .32 .76 .168 4 6HX
GT405032 M5 X 0,8 2.37 .47 .91 .194 4 6HX
GT405033 M6 X 1 2.50 .46 1.01 .255 4 6HX
GT405034 M8 X 1,25 2.71 .48 1.13 .318 4 6HX
GT405035 M10 X 1,5 2.92 .53 1.26 .381 4 6HX
GT405036 M12 X 1,75 3.38 .77 1.74 .367 4 6HX
GT405037 M14 X 2 3.59 .83 1.74 .429 4 6HX
GT405038 M16 X 2 3.81 .91 1.89 .480 4 6HX
䢇
first choice
嘷
alternate choice
High-Performance Taps
Shank Tolerance
D Fractional D Inch
.250–.375 +0, -.0004
.438–.625 +0, -.0004
number
of flutes
class
of fit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A57
Page 57
High-Performance Taps
Victory™Straight-Flute HSS-E-PM Taps • Through and Blind Holes
• GP6520 TiCN for cast iron and cast aluminum.
GT40 • Form C Semi-Bottoming Chamfer • Metric DIN 371 and 376
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT405001 M4 X 0,7 63 10 21 4,5 3 DIN 371 6HX
GT405002 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT405003 M6 X 1 80 10 30 6,0 4 DIN 371 6HX
GT405004 M8 X 1,25 90 13 35 8,0 4 DIN 371 6HX
GT405005 M10 X 1,5 100 15 39 10,0 4 DIN 371 6HX
GT405006 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT405007 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT405008 M16 X 2 110 20 51 12,0 4 DIN 376 6HX
GT405009 M18 X 2,5 125 25 58 14,0 4 DIN 376 6HX
GT405010 M20 X 2,5 140 25 64 16,0 4 DIN 376 6HX
GT405011 M22 X 2,5 140 25 70 18,0 4 DIN 376 6HX
number
of flutes
䢇
first choice
嘷
alternate choice
dimension
standard
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
class
of fit
A58
WWW.WIDIA.COM
Page 58
High-Performance Taps
Victory™Straight-Flute HSS-E-PM Taps • Through and Blind Holes
• GP6520 TiCN for cast iron and cast aluminum.
䢇
first choice
嘷
alternate choice
GT41 • Form C Semi-Bottoming Chamfer • Through Coolant • Metric DIN 371 and 376
12–16 +0, -0,011
GP6520 D1 size L L3 L2 D
GT415001 M4 X 0,7 63 10 21 4,5 3 DIN 371 6HX
GT415002 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT415003 M6 X 1 80 10 30 6,0 4 DIN 371 6HX
GT415004 M8 X 1,25 90 13 35 8,0 4 DIN 371 6HX
GT415005 M10 X 1,5 100 15 39 10,0 4 DIN 371 6HX
GT415006 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT415007 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT415008 M16 X 2 110 20 51 12,0 4 DIN 376 6HX
GT415009 M18 X 2,5 125 25 58 14,0 4 DIN 376 6HX
GT415010 M20 X 2,5 140 25 64 16,0 4 DIN 376 6HX
number
of flutes
dimension
standard
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
Holemaking • High-Performance Taps
class
of fit
WWW.WIDIA.COM
A59
Page 59
High-Performance Taps
Victory™Straight-Flute HSS-E-PM Taps • Threading Close to the Bottom in a Blind Hole
• GP6520 TiCN for cast iron and cast aluminum.
GT42 • Form E Bottoming Chamfer • Metric DIN 371, 374, and 376
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
GP6520 D1 size L L3 L2 D
GT425001 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT425002 M6 X 1 80 10 30 6,0 4 DIN 371 6HX
GT425003 M8 X 1,25 90 13 35 8,0 4 DIN 371 6HX
GT425004 M10 X 1,5 100 15 39 10,0 4 DIN 371 6HX
GT425007 M12 X 1,5 100 15 39 9,0 4 DIN 374 6HX
GT425005 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT425008 M14 X 1,5 100 15 47 11,0 4 DIN 374 6HX
GT425006 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT425009 M16 X 1,5 100 15 46 12,0 4 DIN 374 6HX
number
of flutes
dimension
standard
class
of fit
A60
WWW.WIDIA.COM
Page 60
High-Performance Taps
Victory™Straight-Flute HSS-E-PM Taps • Threading Close to the Bottom in a Blind Hole
• GP6520 TiCN for cast iron and cast aluminum.
䢇
first choice
嘷
alternate choice
GT43 • Form E Bottoming Chamfer • Through Coolant • Metric DIN 371, 374, and 376
Shank Tolerance
D Tolerance h6
6 +0, -0,008
8–10 +0, -0,009
12–16 +0, -0,011
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT435001 M5 X 0,8 70 10 25 6,0 3 DIN 371 6HX
GT435002 M6 X 1 80 10 30 6,0 4 DIN 371 6HX
GT435003 M8 X 1,25 90 13 35 8,0 4 DIN 371 6HX
GT435004 M10 X 1,5 100 15 39 10,0 4 DIN 371 6HX
GT435007 M12 X 1,5 100 15 39 9,0 4 DIN 374 6HX
GT435005 M12 X 1,75 110 18 44 9,0 4 DIN 376 6HX
GT435008 M14 X 1,5 100 15 47 11,0 4 DIN 374 6HX
GT435006 M14 X 2 110 20 52 11,0 4 DIN 376 6HX
GT435009 M16 X 1,5 100 15 46 12,0 4 DIN 374 6HX
number
of flutes
dimension
standard
class
of fit
WWW.WIDIA.COM
A61
Page 61
High-Performance Taps
Victory™Forming Tap HSS-E-PM • Blind and Through Holes
• WP31MG TiN for steel.
• WN38MG DLC for aluminum.
GT22 • Form C Semi-Bottoming Entry Taper • Metric DIN 2174
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
WP31MG WN38MG D1 size L L3 L2 D
GT225016 GT225001 M3 X 0,5 56 6 18 3,5 4 6HX
GT225017 GT225002 M4 X 0,7 63 7 21 4,5 4 6HX
GT225018 GT225003 M5 X 0,8 70 8 25 6,0 4 6HX
GT225019 GT225004 M6 X 1 80 10 30 6,0 5 6HX
GT225024 GT225009 M8 X 1 90 10 35 8,0 5 6HX
GT225020 GT225005 M8 X 1,25 90 14 35 8,0 5 6HX
GT225025 GT225010 M10 X 1 90 10 35 10,0 5 6HX
GT225026 GT225011 M10 X 1,25 100 16 39 10,0 5 6HX
GT225021 GT225006 M10 X 1,5 100 16 39 10,0 5 6HX
GT225027 GT225012 M12 X 1,25 100 15 — 9,0 6 6HX
GT225028 GT225013 M12 X 1,5 100 15 — 9,0 6 6HX
GT225022 GT225007 M12 X 1,75 110 18 — 9,0 6 6HX
GT225029 GT225014 M14 X 1,5 100 15 — 11,0 6 6HX
GT225030 GT225015 M16 X 1,5 100 15 — 12,0 6 6HX
GT225023 GT225008 M16 X 2 110 22 — 12,0 6 6HX
number of
lube grooves
class
of fit
A62
WWW.WIDIA.COM
Page 62
High-Performance Taps
Victory™Forming Tap HSS-E-PM • Blind and Through Holes
• WP31MG TiN for steel.
• WN38MG DLC for aluminum.
䢇
first choice
嘷
alternate choice
GT23 • Form C Semi-Bottoming Entry Taper • Through Coolant • Metric DIN 2174
WP31MG WN38MG D1 size L L3 L2 D
GT235012 GT235001 M5 X 0,8 70 8 25 6,0 4 6HX
GT235013 GT235002 M6 X 1 80 10 30 6,0 5 6HX
GT235018 GT235007 M8 X 1 90 10 35 8,0 5 6HX
GT235014 GT235003 M8 X 1,25 90 14 35 8,0 5 6HX
GT235019 GT235008 M10 X 1 90 10 35 10,0 5 6HX
GT235015 GT235004 M10 X 1,5 100 16 39 10,0 5 6HX
GT235020 GT235009 M12 X 1,5 100 15 — 9,0 6 6HX
GT235016 GT235005 M12 X 1,75 110 18 — 9,0 6 6HX
GT235021 GT235010 M14 X 1,5 100 15 — 11,0 6 6HX
GT235022 GT235011 M16 X 1,5 100 15 — 12,0 6 6HX
GT235017 GT235006 M16 X 2 110 22 — 12,0 6 6HX
Shank Tolerance
D Tolerance h9
1–3 +0, -0,025
3,5–6 +0, -0,030
7–10 +0, -0,036
11–18 +0, -0,043
number of
lube grooves
Holemaking • High-Performance Taps
class
of fit
WWW.WIDIA.COM
A63
Page 63
Victory™GT HP HSS-E-PM Wind Taps
Boost productivity on large-sized components.
• Made with highly alloyed powdered metal HSS-E substrate that combines
wear and heat resistance with toughness.
• GP6520
• Precision h6 shank results in exceptional thread quality and tool life due a very low runout.
• GT20 through holes.
• GT30 and GT31 for blind holes on vertical tapping.
• GT50 and GT51 for blind holes on horizontal tapping.
• All GT
and extra-long lengths as standard.
™
Grade provides long tap life at high tapping speeds.
™
Series Wind Taps are available according to DIN 376
A64
WWW.WIDIA.COM
Page 64
Victory™Left-Hand Spiral-Flute HSS-E-PM Taps • Through Holes
• GP6520 TiCN for steel and cast iron.
GT20 • Form D Plug Chamfer • Large Sizes • Metric DIN 376
High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT205111 M24 X 3 160 30 77 18,0 5 6HX
GT205113 M30 X 3,5 180 35 91 22,0 5 6HX
GT205114 M33 X 3,5 180 35 100 25,0 5 6HX
GT205116 M36 X 4 200 40 110 28,0 6 6HX
GT205118 M42 X 4,5 200 45 120 32,0 6 6HX
GT20 • Form D Plug Chamfer • Larger Sizes • Metric Extra Long
number
of flutes
䢇
first choice
嘷
alternate choice
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
class
of fit
Shank Tolerance
D Tolerance h6
GP6520 D1 size L L3 L2 D
GT205122 M24 X 3 200 30 120 18,0 5 6HX
GT205124 M30 X 3,5 250 35 150 22,0 5 6HX
GT205125 M33 X 3,5 250 35 150 25,0 5 6HX
GT205127 M36 X 4 250 40 150 28,0 6 6HX
GT205129 M42 X 4,5 300 45 180 32,0 6 6HX
WWW.WIDIA.COM
number
of flutes
class
of fit
A65
Page 65
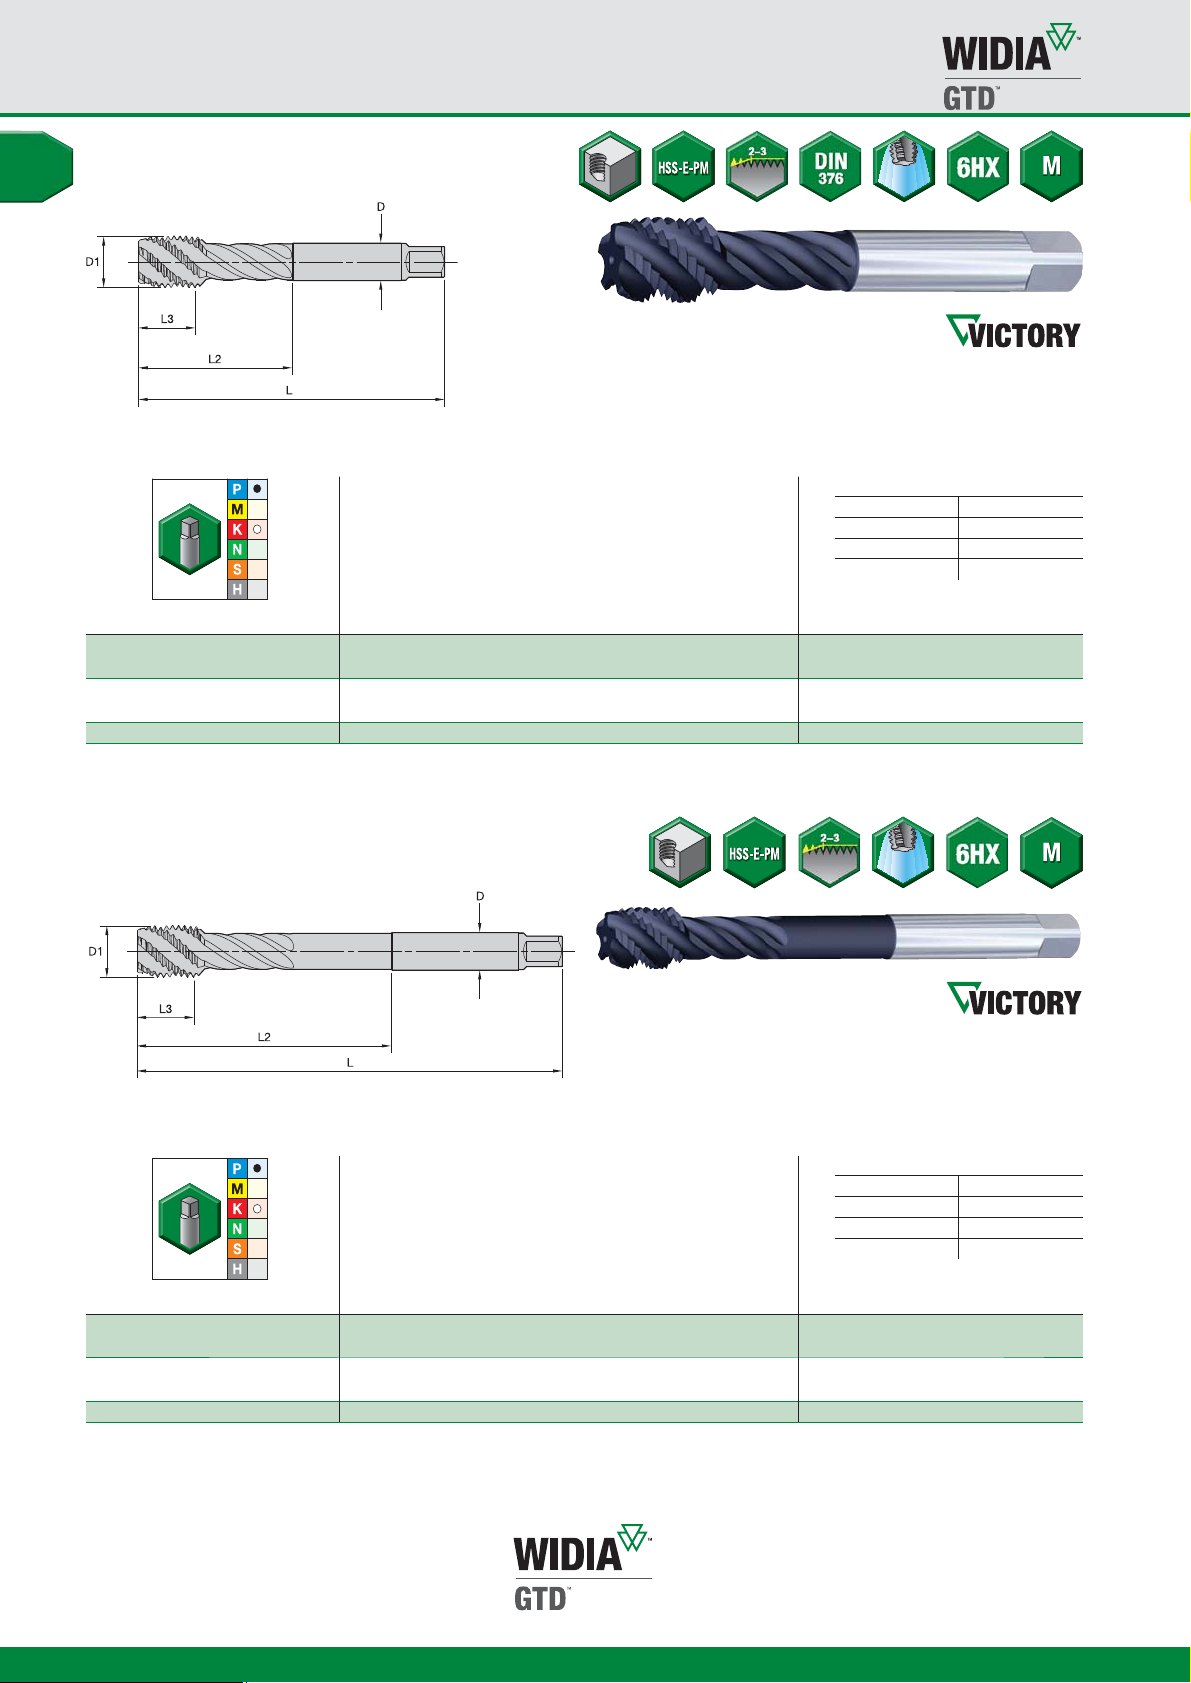
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GP6520 TiCN for steel and cast iron.
GT30 • Form C Semi-Bottoming Chamfer • Larger Sizes • Metric DIN 376
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
GP6520 D1 size L L3 L2 D
GT305161 M24 X 3 160 30 77 18,0 5 6HX
GT305163 M30 X 3,5 180 35 91 22,0 5 6HX
GT305164 M33 X 3,5 180 35 100 25,0 5 6HX
GT305166 M36 X 4 200 40 110 28,0 5 6HX
GT305168 M42 X 4,5 200 45 120 32,0 5 6HX
䢇
first choice
嘷
alternate choice
GT30 • Form C Semi-Bottoming Chamfer • Larger Sizes • Metric Extra Long
number
of flutes
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
class
of fit
A66
GP6520 D1 size L L3 L2 D
GT305151 M24 X 3 200 30 120 18,0 5 6HX
GT305153 M30 X 3,5 250 35 150 22,0 5 6HX
GT305154 M33 X 3,5 250 35 150 25,0 5 6HX
GT305156 M36 X 4 250 40 150 28,0 5 6HX
GT305158 M42 X 4,5 300 45 180 32,0 5 6HX
number
of flutes
class
of fit
WWW.WIDIA.COM
Page 66
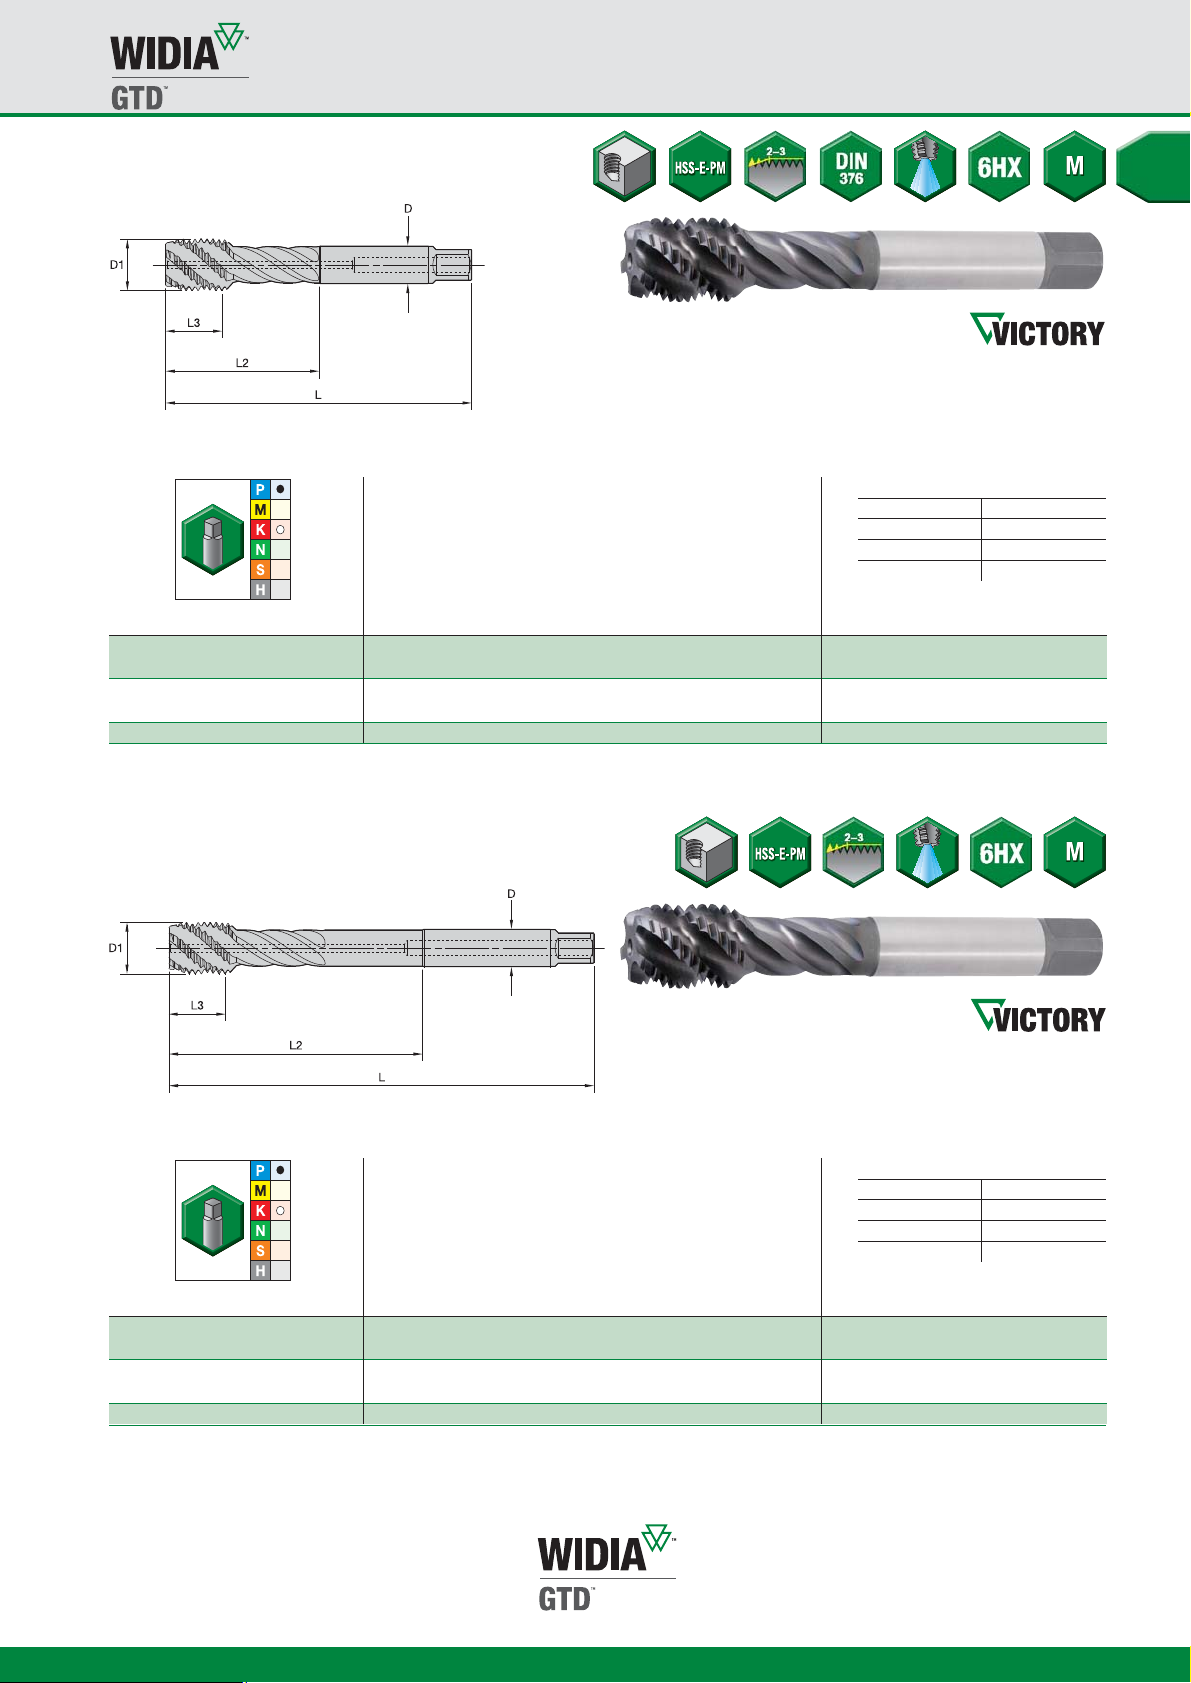
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GP6520 TiCN for steel and cast iron.
䢇
first choice
嘷
alternate choice
GT31 • Form C Semi-Bottoming Chamfer • Through Coolant • Larger Sizes • Metric DIN 376
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT315025 M24 X 3 160 30 77 18,0 5 6HX
GT315027 M30 X 3,5 180 35 91 22,0 5 6HX
GT315028 M33 X 3,5 180 35 100 25,0 5 6HX
GT315030 M36 X 4 200 40 110 28,0 5 6HX
GT315032 M42 X 4,5 200 45 120 32,0 5 6HX
䢇
first choice
嘷
alternate choice
GT31 • Form C Semi-Bottoming Chamfer • Through Coolant • Larger Sizes • Metric Extra Long
number
of flutes
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
class
of fit
GP6520 D1 size L L3 L2 D
GT315014 M24 X 3 200 30 120 18,0 5 6HX
GT315016 M30 X 3,5 250 35 150 22,0 5 6HX
GT315017 M33 X 3,5 250 35 150 25,0 5 6HX
GT315019 M36 X 4 250 40 150 28,0 5 6HX
GT315021 M42 X 4,5 300 45 180 32,0 5 6HX
WWW.WIDIA.COM
number
of flutes
class
of fit
A67
Page 67
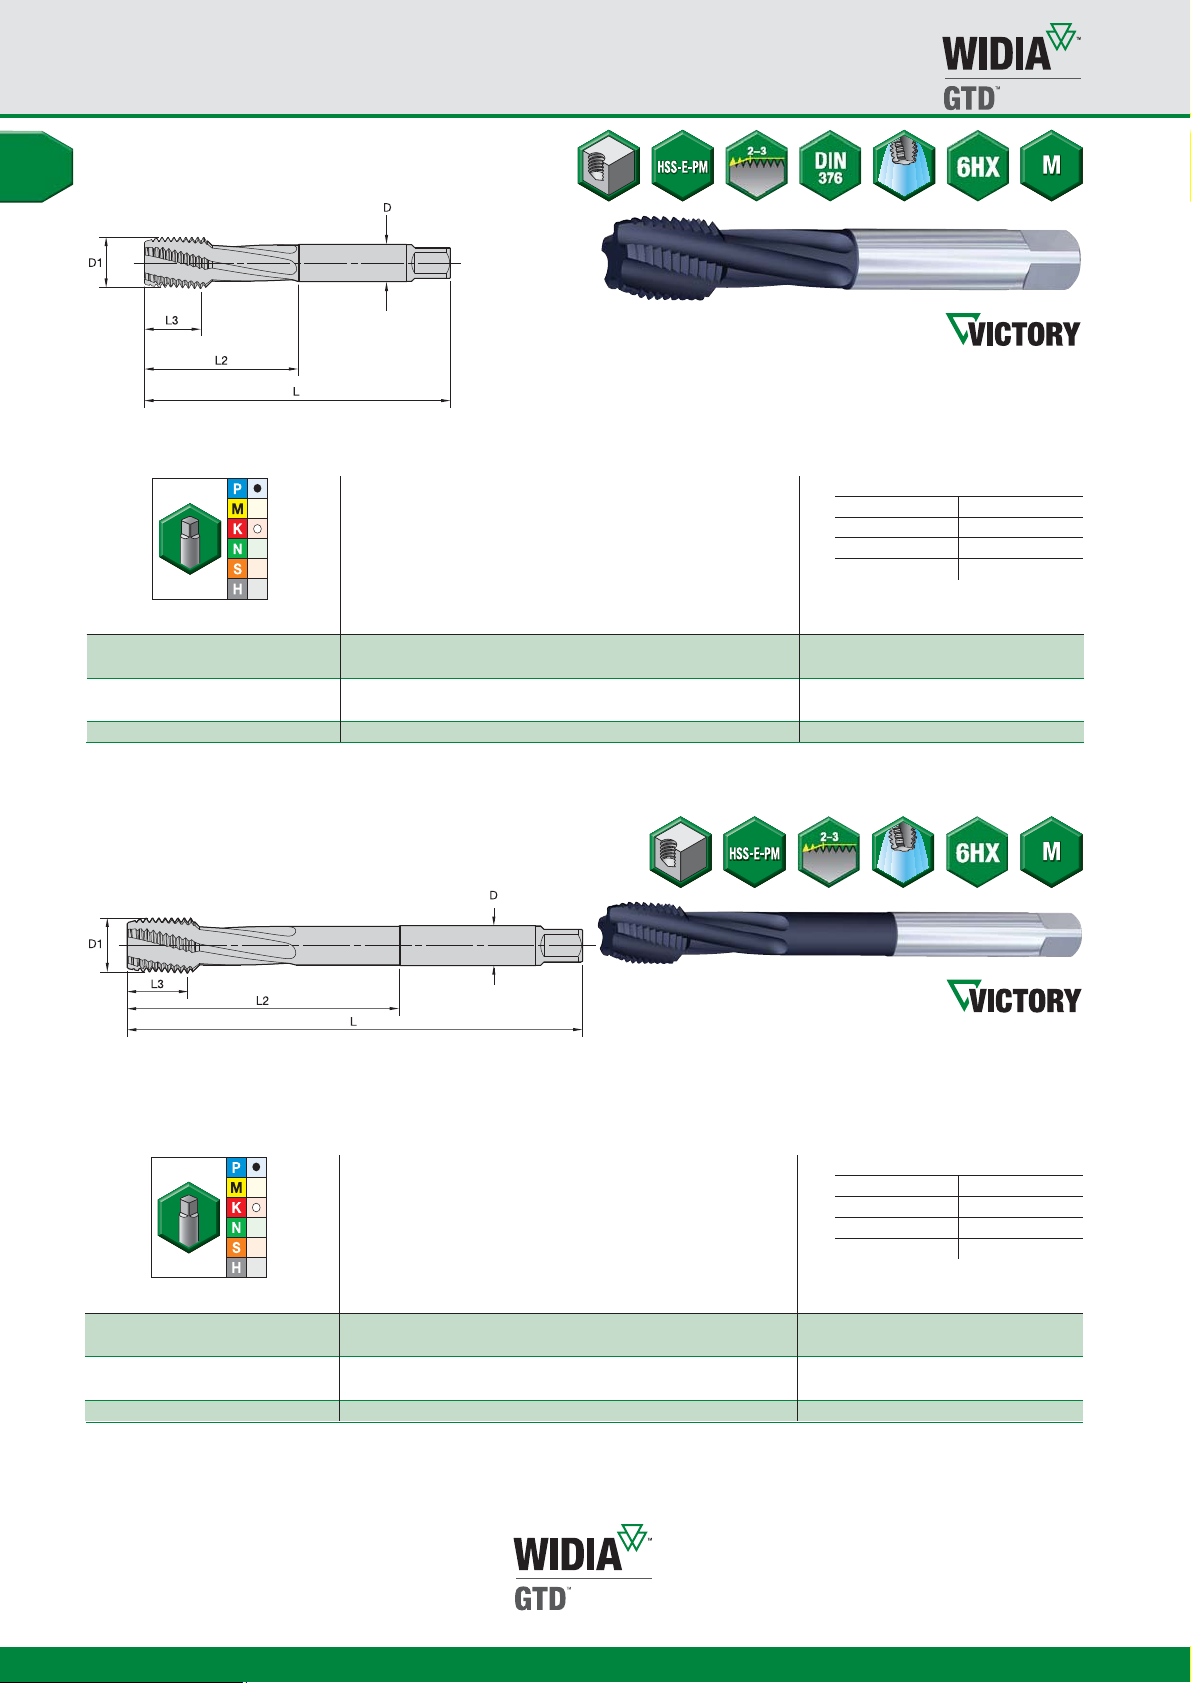
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GP6520 TiCN for steel and cast iron.
GT50 • Form C Semi-Bottoming Chamfer • Larger Sizes • Metric DIN 376
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
Shank Tolerance
D Tolerance h6
GP6520 D1 size L L3 L2 D
GT505001 M24 X 3 160 30 77 18,0 4 6HX
GT505002 M30 X 3,5 180 35 91 22,0 5 6HX
GT505003 M33 X 3,5 180 35 100 25,0 5 6HX
GT505004 M36 X 4 200 40 110 28,0 5 6HX
GT505005 M42 X 4,5 200 45 120 32,0 6 6HX
䢇
first choice
嘷
alternate choice
GT50 • Form C Semi-Bottoming Chamfer • Larger Sizes • Metric Extra Long
number
of flutes
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
class
of fit
A68
GP6520 D1 size L L3 L2 D
GT505006 M24 X 3 200 30 120 18,0 4 6HX
GT505007 M30 X 3,5 250 35 150 22,0 5 6HX
GT505008 M33 X 3,5 250 35 150 25,0 5 6HX
GT505009 M36 X 4 250 40 150 28,0 5 6HX
GT505010 M42 X 4,5 300 45 180 32,0 6 6HX
number
of flutes
class
of fit
WWW.WIDIA.COM
Page 68
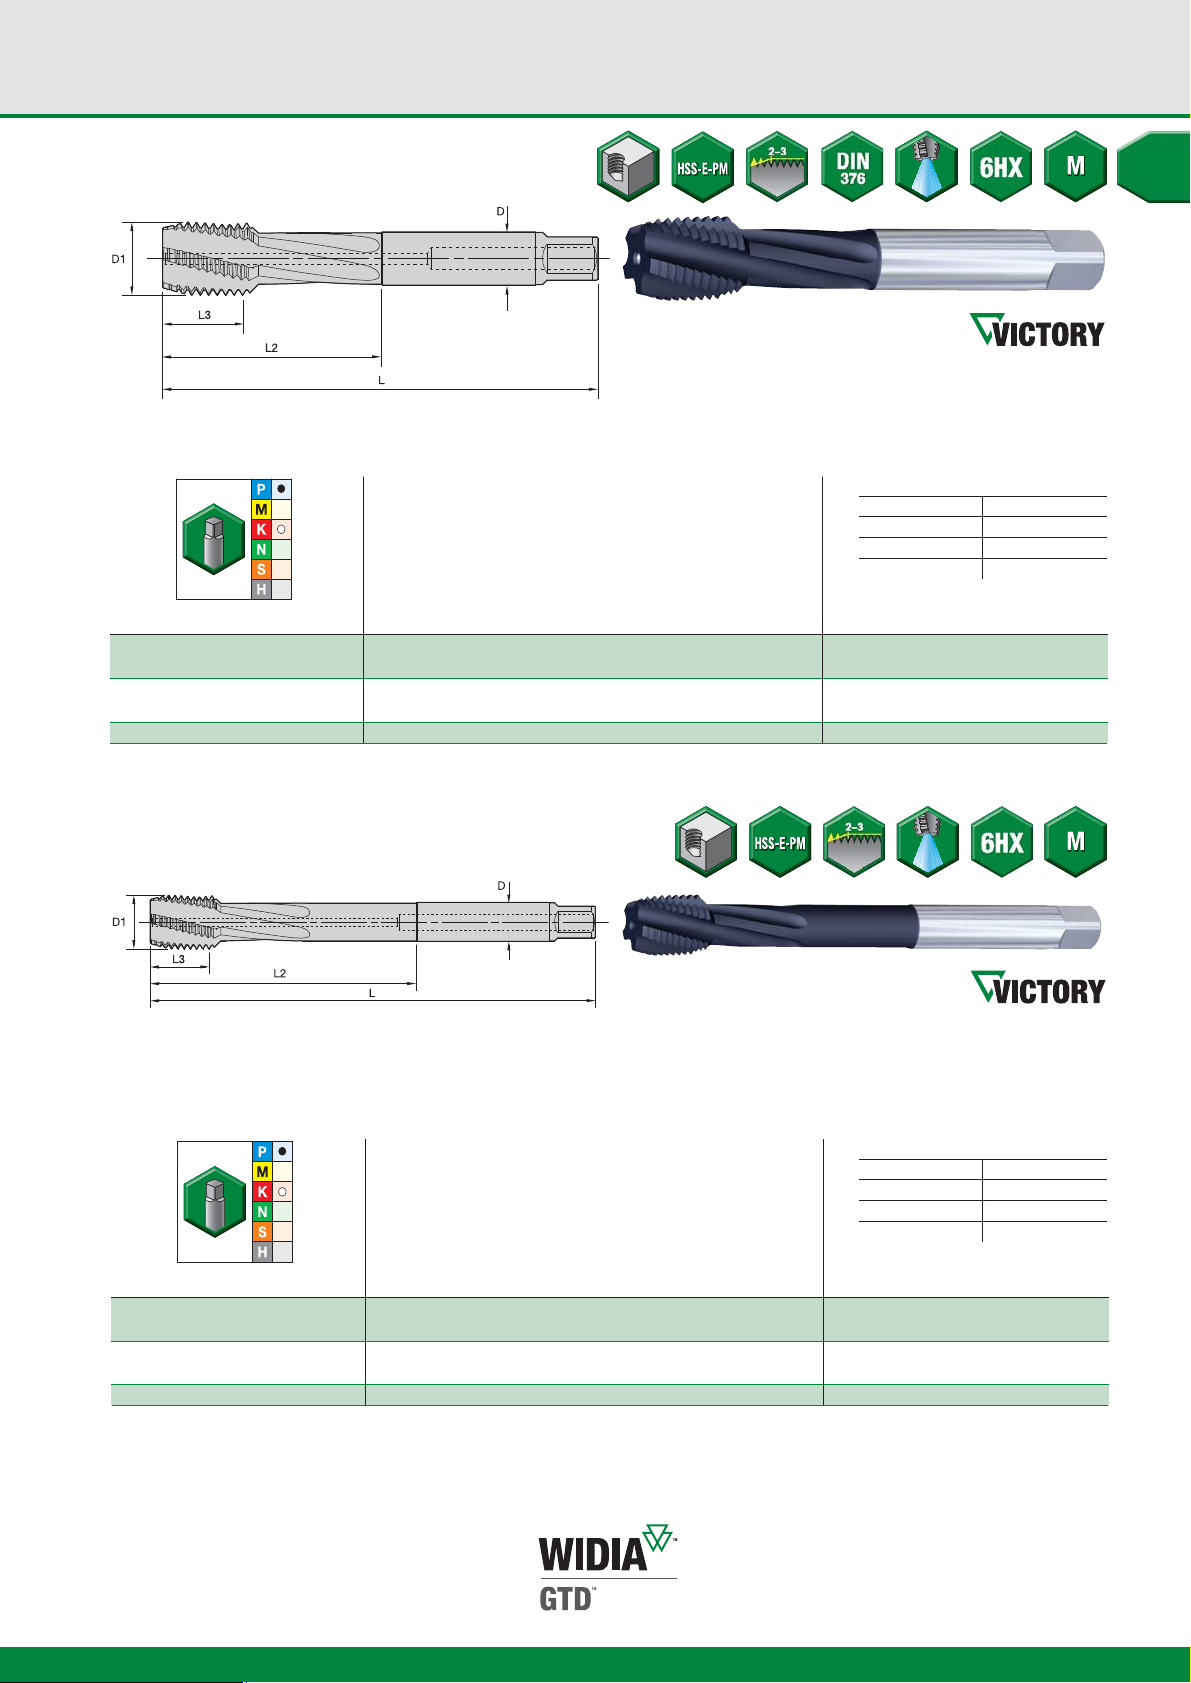
High-Performance Taps
Victory™Spiral-Flute HSS-E-PM Taps • Blind Holes
• GP6520 TiCN for steel and cast iron.
䢇
first choice
嘷
alternate choice
GT51 • Form C Semi-Bottoming Chamfer • Through Hole • Larger Sizes • Metric DIN 376
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
Holemaking • High-Performance Taps
GP6520 D1 size L L3 L2 D
GT515001 M24 X 3 160 30 77 18,0 4 6HX
GT515002 M30 X 3,5 180 35 91 22,0 5 6HX
GT515003 M33 X 3,5 180 35 100 25,0 5 6HX
GT515004 M36 X 4 200 40 110 28,0 5 6HX
GT515005 M42 X 4,5 200 45 120 32,0 6 6HX
䢇
first choice
嘷
alternate choice
GT51 • Form C Semi-Bottoming Chamfer • Through Coolant • Larger Sizes • Metric Extra Long
number
of flutes
Shank Tolerance
D Tolerance h6
12–18 +0, -0,011
20–30 +0, -0,013
32–36 +0, -0,016
class
of fit
GP6520 D1 size L L3 L2 D
GT515006 M24 X 3 200 30 120 18,0 4 6HX
GT515007 M30 X 3,5 250 35 150 22,0 5 6HX
GT515008 M33 X 3,5 250 35 150 25,0 5 6HX
GT515009 M36 X 4 250 40 150 28,0 5 6HX
GT515010 M42 X 4,5 300 45 180 32,0 6 6HX
WWW.WIDIA.COM
number
of flutes
class
of fit
A69
Page 69
High-Performance Taps
Application Data • HSS-E-PM • Metric
Through Holes Blind Holes
Range — m/min Range — m/min
Group Tap Style Grade min
1
2
P
2, 3, 4, 6, 7, GT20 GP6520 12
5, 9, 10, 11 GT00 WP31MG 5
12, 13.1 GT20 GP6520 12
13.2 GT00 WP31MG 6
14.1 GT20 GM6515 12
M
K
Holemaking • High-Performance Taps
N
S
H
NOTE: Increase speed by up to 25% when using coolant taps (GT21, GT23, GT31, GT33, GT41, GT43, and GT51).
14.3 GT20 GM6515 9
14.2, 14.4 GT20 GM6515 8
15, 16 GT40 GP6520 35
17, 18, 19 GT40 GP6520 31
20 GT40 GP6520 23
21
22, 23, 24
26, 27, 28 GT40 GP6520 4
31, 32 GT20 GP6520 8
33, 34, 35 GT10 WS32MG 3
36 GT10 WS32MG 3
37 GT14 WN35MG 3
38.1, 40.1, 40.2 GT06 WN35MG 1,3
38.2, 41.1 GT06 WN35MG 1,0
Use grade GP6505
GT20 GP6520 20
GT22 WP31MG 18
GT20 GP6520 17
GT22 WP31MG 15
GT40 GP6520 38
GT22 WN38MG 33
GT70 WN48EG 42
GT22 WN48EG 37
™
in steels. Use 50% of the recommended speed listed for grade KP6525™.
Starting
Value max Tap Style Grade min
30
30
25
25
15
6
15
8
15
12
10
45
40
30
50
50
55
55
6
12
5
4
4
2,0
1,5
45 GT30, GT32, GT50 GP6520 14
50 GT22 WP31MG 13
38 GT30, GT32, GT50 GP6520 12
42 GT22 WP31MG 10
20 GT30, GT32, GT50 GP6520 8
8 GT02, GT04 WP31MG 3
20 GT30, GT32, GT50 GP6520 8
10 GT02, GT04 WP31MG 4
20 GT30, GT32, GT50 GM6515 8
16 GT30, GT32, GT50 GM6515 6
13 GT30, GT32, GT50 GM6515 5
59 GT40, GT42 GP6520 24
52 GT40, GT42 GP6520 22
39 GT40, GT42 GP6520 16
65 GT40, GT42 GP6520 27
75 GT22 WN38MG 23
72 GT80 WN48EG 30
83 GT22 WN48EG 26
9 GT40, GT42 GP6520 3
18 GT30, GT32 GP6520 6
8 GT12 WS32MG 3
6 GT12 WS32MG 2
6 GT16 WN35MG 2
3,0 GT06 WN35MG 1,1
2,3 GT06 WN35MG 0,8
Starting
Value max
21
21
18
18
11
4
11
6
11
8
7
32
28
21
35
35
39
39
4
8
4
3
3
1,4
1,1
32
35
26
29
14
5
14
7
14
11
9
41
36
27
46
53
50
58
5
11
5
4
4
1,8
1,4
A70
WWW.WIDIA.COM
Page 70
High-Performance Taps
Application Data • HSS-E-PM • Inch
Through Holes Blind Holes
Range — SFM Range — SFM
Group Tap Style Grade min
1
2
P
2, 3, 4, 6, 7, GT20 GP6520 40
5, 9, 10, 11 GT00 WP31MG 15
12, 13.1 GT20 GP6520 40
13.2 GT00 WP31MG 20
14.1 GT20 GM6515 40
M
K
N
S
H
NOTE: Increase speed by up to 25% when using coolant taps (GT21, GT23, GT31, GT33, GT41, GT43, and GT51).
14.3 GT20 GM6515 30
14.2, 14.4 GT20 GM6515 30
15, 16 GT40 GP6520 110
17, 18, 19 GT40 GP6520 100
20 GT40 GP6520 80
21
22, 23, 24
26, 27, 28 GT40 GP6520 13
31, 32 GT20 GP6520 30
33, 34, 35 GT10 WS32MG 11
36 GT10 WS32MG 9
37 GT14 WN35MG 9
38.1, 40.1, 40.2 GT06 WN35MG 4
38.2, 41.1 GT06 WN35MG 3
Use grade GP6505
GT20 GP6520 70
GT22 WP31MG 60
GT20 GP6520 50
GT22 WP31MG 50
GT40 GP6520 130
GT22 WN38MG 110
GT70 WN48EG 140
GT22 WN48EG 120
™
in steels. Use 50% of the recommended speed listed for grade KP6525™.
Starting
Value max Tap Style Grade min
100
100
80
80
50
20
50
30
50
40
30
150
130
100
160
160
180
180
20
40
16
13
13
7
5
150 GT30, GT32, GT50 GP6520 50
160 GT22 WP31MG 40
120 GT30, GT32, GT50 GP6520 40
140 GT22 WP31MG 30
60 GT30, GT32, GT50 GP6520 30
26 GT02, GT04 WP31MG 11
60 GT30, GT32, GT50 GP6520 30
30 GT02, GT04 WP31MG 10
60 GT30, GT32, GT50 GM6515 30
50 GT30, GT32, GT50 GM6515 20
40 GT30, GT32, GT50 GM6515 20
190 GT40, GT42 GP6520 80
170 GT40, GT42 GP6520 70
130 GT40, GT42 GP6520 50
210 GT40, GT42 GP6520 90
250 GT22 WN38MG 80
230 GT80 WN48EG 100
270 GT22 WN48EG 80
30 GT40, GT42 GP6520 11
60 GT30, GT32 GP6520 21
25 GT12 WS32MG 9
20 GT12 WS32MG 7
20 GT16 WN35MG 7
10 GT06 WN35MG 4
7 GT06 WN35MG 3
Starting
Value max
70
70
60
60
30
14
30
20
30
30
20
100
90
70
110
110
130
130
14
28
11
9
9
5
3
100
120
90
100
40
18
40
20
40
40
30
130
120
90
150
170
160
190
18
36
15
12
12
Holemaking • High-Performance Taps
6
4
WWW.WIDIA.COM
A71
Page 71
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
Steel <32 HRC • Selector
HSS-E-PM Taps
PPP
HSS-E-PM Taps
typical
thread sizes
cutting taps
metric inch mm inch fraction wire GT30_GP6520 GT20_GP6520 GT30_GP6520 GT20_GP6520
M3 x 0,50 — 2,500 .0984 — — GT305070 GT205069 GT305097 GT205094
— 6-32 2,705 .1065 — 36 GT305035 GT205037 — —
M4 x 0,70 — 3,300 .1299 — — GT305071 GT205070 GT305098 GT205095
— 8-32 3,454 .1360 — 29 GT305036 GT205039 — —
— 8-36 3,454 .1360 — 29 — GT205052 — —
— 10-24 3,734 .1470 — 26 — GT205040 — —
— 10-32 4,039 .1590 — 21 GT305053 GT205054 — —
M5 x 0,80 — 4,200 .1654 — — GT305072 GT205071 GT305099 GT205096
M6 x 1,00 — 5,000 .1969 — — GT305073 GT205072 GT305100 GT205097
— 1/4-20 5,106 .2010 — 7 GT305039 GT205043 — —
Holemaking • High-Performance Taps
— 1/4-28 5,410 .2130 — 3 GT305055 GT205056 — —
— 5/16-18 6,528 .2570 — F GT305041 GT205045 — —
M8 x 1,25 — 6,700 .2638 — — GT305074 GT205074 GT305101 GT205098
— 5/16-24 6,909 .2720 — I GT305057 GT205057 — —
M8 x 1,00 — 7,000 .2756 — — — — GT305109 GT205104
— 3/8-16 7,938 .3125 5/16 — GT305043 GT205047 — —
— 3/8-24 8,433 .3320 — Q GT305058 GT205058 — —
M10 x 1,50 — 8,500 .3346 — — GT305075 GT205075 GT305102 GT205099
M10 x 1,25 — 8,700 .3425 — — — — GT305111 GT205106
M10 x 1,00 — 9,000 .3543 — — — — GT305110 GT205105
— 7/16-14 9,093 .3580 — T GT305044 GT205048 — —
— 7/16-20 9,921 .3906 25/64 — GT305059 GT205059 — —
M12 x 1,75 — 10,200 .4016 — — GT305076 GT205076 GT305103 GT205100
M12 x 1,50 — 10,500 .4134 — — — — GT305112 GT205107
— 1/2-13 10,716 .4219 27/64 — GT305046 GT205049 — —
— 1/2-20 11,509 .4531 29/64 — GT305060 GT205060 — —
M14 x 2,00 — 12,000 .4724 — — GT305077 — GT305104 GT205101
M14 x 1,50 — 12,500 .4921 — — — — GT305113 GT205108
— 5/8-11 13,495 .5313 17/32 — GT305048 GT205050 — —
M16 x 2,00 — 14,000 .5512 — - GT305078 — GT305105 GT205102
M16 x 1,50 — 14,500 .5709 — — — — GT305114 GT205109
M18 x 2,50 — 15,500 .6102 — — — — GT305106 —
M18 x 1,50 — 16,500 .6496 — — — — GT305115 GT205110
— 3/4-10 16,670 .6563 21/32 — GT305050 GT2050551 — —
M20 x 2,50 — 17,500 .6890 — — — — — GT205103
M22 x 2,50 — 19,500 .7677 — — — — GT305107 —
M24 x 3,00 — 21,000 .8268 — — — — GT305161 GT205111
— 1-8 22,225 .8750 7/8 — GT305051 — — —
required
tap drill diameter
blind hole through hole blind hole through hole
ANSI
DIN 371, 374, 376
A72
WWW.WIDIA.COM
Page 72
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
P
HSS-E-PM Taps
Recommended Drill
P
All Materials
Alternate Tap Drill
DIN 371, 374, 376
blind hole through hole approximately 5 x D approximately 5 x D approximately 5 x D approximately 5 x D
with coolant with coolant with coolant non-coolant with coolant non-coolant
GT31_GP6520 GT21_GP6520 TDS402 WP20PD TDS202 WP20PD VDS402A WU25PD VDS202A WU25PD
— — TDS402A02500 TDS202A02500 VDS402A02500 VDS202A02500
— — TDS402A02705 TDS202A02705 VDS402A02705 VDS202A02705
— — TDS402A03300 TDS202A03300 VDS402A03300 VDS202A03300
— — TDS402A03454 TDS202A03454 VDS402A03454 VDS202A03454
— — TDS402A03700 TDS202A03700 VDS402A03700 VDS202A03700
— — TDS402A03797 TDS202A03797 VDS402A03797 VDS202A03797
— — TDS402A04100 TDS202A04100 VDS402A04100 VDS202A04100
GT315007 GT215007 TDS402A04219 TDS202A04219 VDS402A04219 VDS202A04219
GT315008 GT215008 TDS402A05055 TDS202A05055 VDS402A05055 VDS202A05055
— — TDS402A05410 TDS202A05410 VDS402A05410 VDS202A05410
— — TDS402A05600 TDS202A05600 VDS402A05600 VDS202A05600
— — TDS402A06600 TDS202A06600 VDS412A06600 VDS212A06600
GT315009 GT215009 TDS402A06906 TDS202A06906 VDS412A06906 VDS212A06906
— — TDS402A07000 TDS202A07000 VDS412A07000 VDS212A07000
— — TDS402A07366 TDS202A07366 VDS412A07366 VDS212A07366
— — TDS402A08433 TDS202A08433 VDS412A08433 VDS212A08433
— — TDS402A08500 TDS202A08500 VDS412A08500 VDS212A08500
GT315010 GT215010 TDS402A08700 TDS202A08700 VDS412A08700 VDS212A08700
— — TDS402A09000 TDS202A09000 VDS412A09000 VDS212A09000
— — TDS402A08839 TDS202A08839 VDS412A08839 VDS212A08839
— — TDS402A09400 TDS202A09400 VDS412A09400 VDS212A09400
— — TDS402A10200 TDS202A10200 VDS412A10200 VDS212A10200
GT315011 GT215011 TDS402A10262 TDS202A10262 VDS412A10262 VDS212A10262
— — TDS402A10716 TDS202A10716 VDS412A10716 VDS212A10716
— — TDS402A10800 TDS202A10800 VDS412A10800 VDS212A10800
— — TDS402A11908 TDS202A11908 VDS412A11908 VDS212A11908
GT315012 GT215012 TDS402A12251 TDS202A12251 VDS412A12251 VDS212A12251
— — TDS402A12800 TDS202A12800 VDS412A12800 VDS212A12800
— — TDS402A13500 TDS202A13500 VDS412A13500 VDS212A13500
— — TDS402A14500 TDS202A14500 VDS412A14500 VDS212A14500
— — TDS402A14684 TDS202A14684 VDS412A14684 VDS212A14684
— — TDS402A16500 TDS202A16500 VDS412A16500 VDS212A16500
— — TDS402A16670 TDS202A16670 VDS412A16670 VDS212A16670
— — TDS402A17000 TDS202A17000 VDS412A17000 VDS212A17000
— — TDS402A17859 TDS202A17859 VDS412A17859 VDS212A17859
——— — — —
GT315025 — TDM220R3SCF25M TDM220R5SCF25M — —
— — TDM230R3SCF25M TDM230R5SCF25M — —
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A73
Page 73
High-Performance Taps
Cross Reference Chart • HSS-E-PM • Forming Taps and Drills
Steel 32–44 HRC • Selector
HSS-E-PM Taps — Tapping Steel 32–44 HRC
P
Holemaking • High-Performance Taps
typical
thread sizes
cutting taps
metric mm inch GT02_WP31MG GT04_WH36MG GT00_WP31MG
M3 x 0,50 2,500 .0984 GT025001 GT045001 GT005001
M4 x 0,70 3,300 .1299 GT025002 GT045002 GT005002
M5 x 0,80 4,200 .1654 GT025003 GT045003 GT005003
M6 x 1,00 5,000 .1969 GT025004 GT045004 GT005004
M8 x 1,25 6,700 .2638 GT025005 GT045005 GT005005
M8 x 1,00 7,000 .2756 GT025012 GT045012 GT005012
M10 x 1,50 8,500 .3346 GT025006 GT045006 GT005006
M10 x 1,25 8,700 .3425 GT025014 GT045014 GT005014
M10 x 1,00 9,000 .3543 GT025013 GT045013 GT005013
M12 x 1,75 10,200 .4016 GT025007 GT045007 GT005007
M12 x 1,50 10,500 .4134 GT025016 GT045016 GT005016
M12 x 1,25 10,800 .4252 GT025015 GT045015 GT005015
M14 x 2,00 12,000 .4724 GT025008 GT045008 GT005008
M14 x 1,50 12,500 .4921 GT025017 GT045017 GT005017
M16 x 2,00 14,000 .5512 GT025009 GT045009 GT005009
M16 x 1,50 14,500 .5709 GT025018 GT045018 GT005018
M18 x 2,50 15,500 .6102 GT025010 GT045010 GT005010
M18 x 1,50 16,500 .6496 GT025010 GT045010 GT005010
M20 x 2,50 17,500 .6890 GT025011 GT045011 GT005011
required
tap drill diameter
DIN 371, 374, 376
blind hole blind hole (3 x D) through hole
Steel • Selector
P
Steel <32 HRC — Forming Tap
typical
thread sizes
cutting taps
metric mm inch GT22_WP31MG GT23_WP31MG
M3 x 0,50 2,800 .1102 GT225016 —
M4 x 0,70 3,700 .1457 GT225017 —
M5 x 0,80 4,700 .1850 GT225018 GT235012
M6 x 1,00 5,600 .2205 GT225019 GT235013
M8 x 1,25 7,400 .2913 GT225020 GT235014
M8 x 1,00 7,600 .2992 GT225024 GT235018
M10 x 1,50 9,400 .3701 GT225021 GT235015
M10 x 1,25 9,500 .3740 GT225026 —
M10 x 1,00 9,500 .3740 GT225025 GT235019
M12 x 1,75 11,300 .4449 GT225022 GT235016
M12 x 1,50 11,300 .4449 GT225028 GT235020
M12 x 1,25 11,500 .4528 GT225027 —
M14 x 1,50 13,400 .5276 GT225029 GT235021
M16 x 2,00 15,200 .5984 GT225023 GT235017
M16 x 1,50 15,400 .6063 GT225030 GT235022
required
tap drill diameter
DIN 2174
blind and through hole with coolant
blind and through hole
A74
WWW.WIDIA.COM
Page 74
High-Performance Taps
Cross Reference Chart • HSS-E-PM • Forming Taps and Drills
Recommended SC Drill
P
approximately 5 x D approximately 5 x D approximately 5 x D approximately 5 x D
with coolant without coolant with coolant non-coolant
TDS402 WP20PD TDS202 WP20PD VDS402A WU25PD VDS202A WU25PD
TDS402A02500 TDS202A02500 VDS402A02500 VDS202A02500
TDS402A03300 TDS202A03300 VDS402A03300 VDS202A03300
TDS402A04219 TDS202A04219 VDS402A04219 VDS202A04219
TDS402A05055 TDS202A05055 VDS402A05055 VDS202A05055
TDS402A06906 TDS202A06906 VDS412A06906 VDS212A06906
TDS402A07366 TDS202A07366 VDS412A07366 VDS212A07366
TDS402A08700 TDS202A08700 VDS412A08700 VDS212A08700
TDS402A09000 TDS202A09000 VDS412A09000 VDS212A09000
TDS402A08839 TDS202A08839 VDS412A08839 VDS212A08839
TDS402A10262 TDS202A10262 VDS412A10262 VDS212A10262
TDS402A10716 TDS202A10716 VDS412A10716 VDS212A10716
TDS402A11300 TDS202A11300 VDS412A11300 VDS212A11300
TDS402A12251 TDS202A12251 VDS412A12251 VDS212A12251
TDS402A12800 TDS202A12800 VDS412A12800 VDS212A12800
TDS402A14500 TDS202A14500 VDS412A14500 VDS212A14500
TDS402A14684 TDS202A14684 VDS412A14684 VDS212A14684
TDS402A16500 TDS202A16500 VDS412A16500 VDS212A16500
TDS402A16670 TDS202A16670 VDS412A16670 VDS212A16670
TDS402A17859 TDS202A17859 VDS412A17859 VDS212A17859
All Materials
Alternate Tap Drill
Holemaking • High-Performance Taps
P
Recommended SC Drill
approximately 5 x D approximately 5 x D approximately 5 x D approximately 5 x D
with coolant without coolant with coolant non-coolant
TDS402 WP20PD TDS202 WP20PD VDS402A WU25PD VDS202A WU25PD
TDS402A02800 TDS202A02800 VDS402A02800 VDS202A02800
TDS402A03734 TDS202A03734 VDS402A03734 VDS202A03734
TDS402A05000 TDS202A05000 VDS402A05000 VDS202A05000
TDS402A05791 TDS202A05791 VDS402A05791 VDS202A05791
TDS402A07493 TDS202A07493 VDS412A07493 VDS212A07493
TDS402A07938 TDS202A07938 VDS412A07938 VDS212A07938
TDS402A09500 TDS202A09500 VDS412A09500 VDS212A09500
TDS402A09500 TDS202A09500 VDS412A09500 VDS212A09500
TDS402A09921 TDS202A09921 VDS412A09921 VDS212A09921
TDS402A11300 TDS202A11300 VDS412A11300 VDS212A11300
TDS402A11500 TDS202A11500 VDS412A11500 VDS212A11500
TDS402A11509 TDS202A11509 VDS412A11509 VDS212A11509
TDS402A13400 TDS202A13400 VDS412A13400 VDS212A13400
TDS402A15250 TDS202A15250 VDS412A15250 VDS212A15250
TDS402A15500 TDS202A15500 VDS412A15500 VDS212A15500
All Materials
Alternate Tap Drill
WWW.WIDIA.COM
A75
Page 75
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
Stainless Steel • Selector
HSS-E-PM Taps
M
HSS-E-PM Taps
typical
thread sizes
cutting taps
metric inch mm inch fraction wire GT30_GM6515 GT20_GM6515 GT30_GM6515 GT20_GM6515
M3 x 0,50 — 2,500 .0984 — — GT305061 GT205061 GT305148 GT205077
— 6-32 2,705 .1065 — 36 GT305005 GT205007 — —
M4 x 0,70 — 3,300 .1299 — — GT305062 GT205062 GT305079 GT205078
— 8-32 3,454 .1360 — 29 GT305006 GT205008 — —
— 8-36 3,454 .1360 — 29 — GT205022 — —
— 10-24 3,734 .1470 — 26 GT305007 GT205010 — —
— 10-32 4,039 .1590 — 21 GT305023 GT205024 — —
M5 x 0,80 — 4,200 .1654 — — GT305063 GT205063 GT305080 GT205079
— 12-24 4,496 .1770 — 16 — GT205011 — —
M6 x 1,00 5,000 .1969 — — GT305064 GT205064 GT305081 GT205080
Holemaking • High-Performance Taps
— 1/4-20 5,106 .2010 — 7 GT305009 GT205013 — —
— 1/4-28 5,410 .2130 — 3 GT305025 GT205026 — —
— 5/16-18 6,528 .2570 — F GT305011 GT205015 — —
M8 x 1,25 — 6,700 .2638 — — GT305065 GT205066 GT305082 GT205081
— 5/16-24 6,909 .2720 — I GT305027 GT205027 — —
M8 x 1,00 7.000 0,2756 — — — — GT305090 GT205087 —
— 3/8-16 7,938 .3125 5/16 — GT305013 GT205017 — —
— 3/8-24 8,433 .3320 — Q GT305028 GT205028 — —
M10 x 1,50 — 8,500 .3346 — — GT305066 GT205067 GT305083 GT205082
M10 x 1,25 8.700 0,3425 — — — — GT305092 GT205089 —
M10 x 1,00 9.000 0,3543 — — — — GT305091 GT205088 —
— 7/16-14 9,093 .3580 — T GT305014 GT205018 — —
— 7/16-20 9,921 .3906 25/64 — GT305029 GT205029 — —
M12 x 1,75 — 10,200 .4016 — — GT305067 GT205068 GT305084 GT205083
M12 x 1,50 — 10,500 .4134 — — — — GT305093 GT205090
— 1/2-13 10,716 .4219 27/64 — GT305016 GT205019 — —
— 1/2-20 11,509 .4531 29/64 — GT305030 GT205030 — —
M14 x 2,00 — 12,000 .4724 — — GT305068 — GT305085 GT205084
M14 x 1,50 — 12,500 .4921 — — — — GT305094 GT205091
— 5/8-11 13,495 .5313 17/32 — GT305018 GT205020 ——
M16 x 2,00 — 14,000 .5512 — — GT305069 — GT305086 GT205085
M16 x 1,50 — 14,500 .5709 — — — — GT305095 GT205092
M18 x 2,50 — 15,500 .6102 — — — — GT305087 —
M18 x 1,50 — 16,500 .6496 — — — — GT305096 GT205093
— 3/4-10 16,670 .6563 21/32 — GT305020 GT205021 — —
M20 x 2,50 — 17,500 .6890 — — — — — GT205086
M22 x 2,50 — 19,500 .7677 — — — — GT305088 —
required
tap drill diameter
blind hole through hole blind hole through hole
ANSI
DIN 371, 374, 376
M24 x 3,00 — 21,000 .8268 — — — — GT305089 —
— 1—8 22,225 .8750 7/8 — GT305021 — — —
A76
WWW.WIDIA.COM
Page 76
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
HSS-E-PM Taps
M
Recommended SC Drill
All Materials
Alternate Tap Drill
DIN 371, 374, 376
blind hole through hole approximately 3 x D approximately 5 x D approximately 3 x D approximately 5 x D
with coolant with coolant with coolant with coolant with coolant with coolant
GT31_GM6515 GT21_GM6515 WD 412522 WD 412527 VDS401A WU25PD VDS402A WU25PD
— — — — VDS401A02500 VDS402A02500
— — — — VDS401A02705 VDS402A02705
— — 412522—00330 412527—00330 VDS401A03300 VDS402A03300
— — — — VDS401A03454 VDS402A03454
— — — — VDS401A03454 VDS402A03454
— — — — VDS401A03734 VDS402A03734
— — — — VDS401A04039 VDS402A04039
GT315001 GT215001 412522—00420 412527—00420 VDS401A04200 VDS402A04200
— — — — VDS401A04496 VDS402A04496
GT315002 GT215002 412522—00500 412527—00500 VDS401A05000 VDS402A05000
— — — — VDS401A05106 VDS402A05106
— — — — VDS401A05410 VDS402A05410
— — 412522—00652 412527—00652 VDS401A06528 VDS402A06528
GT315003 GT215003 412522—00670 412527—00670 VDS411A06700 VDS412A06700
— — — — VDS411A06906 VDS412A06906
— — 412522—00700 412527—00700 VDS411A07000 VDS412A07000
— — 412522—00793 412527—00793 VDS411A07938 VDS412A07938
— — — — VDS411A08433 VDS412A08433
GT315004 GT215004 412522—00850 412527—00850 VDS411A08500 VDS412A08500
— — 412522—00870 412527—00870 VDS411A08700 VDS412A08700
— — 412522—00900 412527—00900 VDS411A09000 VDS412A09000
— — — — VDS411A09093 VDS412A09093
— — 412522—00992 412527—00992 VDS411A09921 VDS412A09921
GT315005 GT215005 412522—01020 412527—01020 VDS411A10200 VDS412A10200
— — 412522—01050 412527—01050 VDS411A10500 VDS412A10500
— — 412522—01072 412527—01072 VDS411A10716 VDS412A10716
— — — — VDS411A11509 VDS412A11509
GT315006 GT215006 412522—01200 412527—01200 VDS411A12000 VDS412A12000
— — 412522—01250 412527—01250 VDS411A12500 VDS412A12500
————VDS411A13495 VDS412A13495
— — 412522—01400 412527—01400 VDS411A14000 VDS412A14000
— — 412522—01450 412527—01450 VDS411A14500 VDS412A14500
— — 412522—01550 412527—01550 VDS411A15500 VDS412A15500
— — 412522—01650 412527—01650 VDS411A16500 VDS412A16500
— — — — VDS411A16670 VDS412A16670
— — 412522—01750 412527—01750 VDS411A17500 VDS412A17500
— — 412522—01950 412527—01950 VDS411A19500 VDS412A19500
Recommended Modular Drill
insert tool body 3 x D
— — TDM2100UPM TDM210R3SCF25M — —
— — TDM2223UPM TDM0886R3SS088 — —
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A77
Page 77
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
Cast Iron • Selector
HSS-E-PM Taps
KK
Recommended SC Drill
typical
thread sizes
cutting taps
metric inch mm inch fraction wire GT40_GP6520 GT40_GP6520 GT41_GP6520 TDS411 WK15PD
M3 x 0,50 — 2,500 .0984 — — GT405030 — — TDS401A02500
M4 x 0,70 — 3,300 .1299 — — GT405031 GT405001 GT415001 TDS401A03300
— 10-24 3,734 .1470 — 26 GT405012 — — TDS401A03734
— 10-32 4,039 .1590 — 21 GT405013 — — TDS401A04039
M5 x 0,80 — 4,200 .1654 — — GT405032 GT405002 GT415002 TDS401A04200
M6 x 1,00 — 5,000 .1969 — — GT405033 GT405003 GT415003 TDS401A05000
— 1/4-20 5,106 .2010 — 7 GT405015 — — TDS401A05106
— 1/4-28 5,410 .2130 — 3 GT405017 — — TDS401A05410
— 5/16-18 6,528 .2570 — F GT405019 — — TDS401A06528
M8 x 1,25 — 6,700 .2638 — — GT405034 GT405004 GT415004 TDS411A06700
Holemaking • High-Performance Taps
— 5/16-24 6,909 .2720 — I GT405020 — — TDS411A06906
— 3/8-16 7,938 .3125 5/16 — GT405022 — — TDS411A07938
— 3/8-24 8,433 .3320 — Q GT405023 — — TDS411A08433
M10 x 1,50 — 8,500 .3346 — — GT405035 GT405005 GT415005 TDS411A08500
— 7/16-14 9,093 .3580 — T GT405024 — — TDS411A09093
— 7/16-20 9,921 .3906 25/64 — GT405025 — — TDS411A09921
M12 x 1,75 — 10,200 .4016 — — GT405036 GT405006 GT415006 TDS411A10200
— 1/2-13 10,716 .4219 27/64 — GT405026 — — TDS411A10716
— 1/2-20 11,509 .4531 29/64 — GT405027 — — TDS411A11509
M14 x 2,00 — 12,000 .4724 — — GT405037 GT405007 GT415007 TDS411A12000
— 5/8-11 13,495 .5313 17/32 — GT405028 — — TDS411A13495
M16 x 2,00 — 14,000 .5512 — — GT405038 GT405008 GT415008 TDS411A14000
M18 x 2,50 — 15,500 .6102 — — — GT405009 GT415009 TDS411A15500
— 3/4-10 16,670 .6563 21/32 — GT405029 — — TDS411A16670
M20 x 2,50 — 17,500 .6890 — — — GT405010 GT415010 TDS411A17500
M22 x 2,50 — 19,500 .7677 — — — GT405011 — TDS411A19500
required
tap drill diameter
ANSI
blind and through hole blind and through hole with coolant with coolant
DIN 371, 374, 376
blind and through hole approximately 3 x D
A78
WWW.WIDIA.COM
Page 78
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
K
Recommended SC Drill
approximately 5 x D approximately 5 x D approximately 3 x D approximately 5 x D approximately 5 x D
with coolant non-coolant with coolant with coolant non-coolant
TDS412 WK15PD TDS212 WK15PD VDS401A WU25PD VDS402A WU25PD VDS202A WU25PD
TDS402A02500 TDS212A02500 VDS401A02500 VDS402A02500 VDS202A02500
TDS402A03300 TDS212A03300 VDS401A03300 VDS402A03300 VDS202A03300
TDS402A03734 TDS212A03734 VDS401A03734 VDS402A03734 VDS202A03734
TDS402A04039 TDS212A04039 VDS401A04039 VDS402A04039 VDS202A04039
TDS402A04200 TDS212A04200 VDS401A04200 VDS402A04200 VDS202A04200
TDS402A05000 TDS212A05000 VDS401A05000 VDS402A05000 VDS202A05000
TDS402A05106 TDS212A05106 VDS401A05106 VDS402A05106 VDS202A05106
TDS402A05410 TDS212A05410 VDS401A05410 VDS402A05410 VDS202A05410
TDS402A06528 TDS212A06528 VDS401A06528 VDS402A06528 VDS202A06528
TDS412A06700 TDS212A06700 VDS411A06700 VDS412A06700 VDS212A06700
TDS412A06906 TDS212A06906 VDS411A06906 VDS412A06906 VDS212A06906
TDS412A07938 TDS212A07938 VDS411A07938 VDS412A07938 VDS212A07938
TDS412A08433 TDS212A08433 VDS411A08433 VDS412A08433 VDS212A08433
TDS412A08500 TDS212A08500 VDS411A08500 VDS412A08500 VDS212A08500
TDS412A09093 TDS212A09093 VDS411A09093 VDS412A09093 VDS212A09093
TDS412A09921 TDS212A09921 VDS411A09921 VDS412A09921 VDS212A09921
TDS412A10200 TDS212A10200 VDS411A10200 VDS412A10200 VDS212A10200
TDS412A10716 TDS212A10716 VDS411A10716 VDS412A10716 VDS212A10716
TDS412A11509 TDS212A11509 VDS411A11509 VDS412A11509 VDS212A11509
TDS412A12000 TDS212A12000 VDS411A12000 VDS412A12000 VDS212A12000
TDS412A13495 TDS212A13495 VDS411A13495 VDS412A13495 VDS212A13495
TDS412A14000 TDS212A14000 VDS411A14000 VDS412A14000 VDS212A14000
TDS412A15500 TDS212A15500 VDS411A15500 VDS412A15500 VDS212A15500
TDS412A16670 TDS212A16670 VDS411A16670 VDS412A16670 VDS212A16670
TDS412A17500 TDS212A17500 VDS411A17500 VDS412A17500 VDS212A17500
TDS412A19500 TDS212A19500 VDS411A19500 VDS412A19500 VDS212A19500
All Materials
Alternate Tap Drill
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A79
Page 79
N
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
Aluminum • Selector
N
HSS-E-PM Taps (Wrought, low Si)
HSS-E-PM Taps (Cast <12%)
typical
thread sizes
cutting taps
metric inch mm inch fraction wire GT80_WN48EG GT70_WN48EG GT40_GP6520
M3 x 0,50 — 2,500 .0984 — — GT805001 GT705001 GT405030
M4 x 0,70 — 3,300 .1299 — — GT805002 GT705002 GT405031
— 10-24 3,734 .1470 — 26 — — GT405012
— 10-32 4,039 .1590 — 21 — — GT405013
M5 x 0,80 — 4,200 .1654 — — GT805003 GT705003 GT405032
M6 x 1,00 — 5,000 .1969 — — GT805004 GT705004 GT405033
— 1/4-20 5,106 .2010 — 7 — — GT405015
— 1/4-28 5,410 .2130 — 3 — — GT405017
— 5/16-18 6,528 .2570 — F — — GT405019
Holemaking • High-Performance Taps
M8 x 1,25 — 6,700 .2638 — — GT805005 GT705005 GT405034
— 5/16-24 6,909 .2720 — I — — GT405020
— 3/8-16 7,938 .3125 5/16 — — — GT405022
— 3/8-24 8,433 .3320 — Q — — GT405023
M10 x 1,50 — 8,500 .3346 — — GT805006 GT705006 GT405035
— 7/16-14 9,093 .3580 — T — — GT405024
— 7/16-20 9,921 .3906 25/64 — — — GT405025
M12 x 1,75 — 10,200 .4016 — — GT805007 GT705007 GT405036
— 1/2-13 10,716 .4219 27/64 — — — GT405026
— 1/2-20 11,509 .4531 29/64 — — — GT405027
M14 x 2,00 — 12,000 .4724 — — — — GT405037
— 5/8-11 13,495 .5313 17/32 — — — GT405028
M16 x 2,00 — 14,000 .5512 — — GT805008 GT705008 GT405038
M18 x 2,50 — 15,500 .6102 — — —— —
— 3/4-10 16,670 .6563 21/32 — — — GT405029
M20 x 2,50 — 17,500 .6890 — — GT805009 — —
M22 x 2,50 — 19,500 .7677 — — —— —
required
tap drill diameter
blind hole through hole blind and through hole
DIN 371, 374, 376
ANSI
Aluminum • Forming Taps • Selector
N
Forming Taps
typical
thread sizes
cutting taps
metric mm inch GT22 WN38MG GT23 WN38MG
M3 x 0,50 2,800 .1102 GT225001 —
M4 x 0,70 3,734 .1470 GT225002 —
M5 x 0,80 4,700 .1850 GT225003 GT235001
M6 x 1,00 5,600 .2205 GT225004 GT235002
M8 x 1,25 7,400 .2913 GT225005 GT235003
M8 x 1,00 7,600 .2992 GT225009 GT235007
M10 x 1,50 9,400 .3701 GT225006 GT235004
M10 x 1,25 9,500 .3740 GT225011 —
M10 x 1,00 9,500 .3740 GT225010 GT235008
M12 x 1,75 11,300 .4449 GT225007 GT235005
M12 x 1,50 11,300 .4449 GT225013 GT235019
M12 x 1,25 11,500 .4528 GT225012 —
M14 x 1,50 13,400 .5276 GT225014 GT235010
M16 x 2,00 15,200 .5984 GT225008 GT235006
M16 x 1,50 15,400 .6063 GT225015 GT235011
required
tap drill diameter
DIN 2174
blind and through hole with coolant
blind and through hole
A80
WWW.WIDIA.COM
Page 80
High-Performance Taps
Cross Reference Chart • HSS-E-PM Taps and Drills
N
HSS-E-PM Taps (Cast <12%)
N
Recommended SC Drill
All Materials
Alternate Tap Drill
DIN 371, 374, 376
blind and through hole approximately 3 x D approximately 3 x D approximately 5 x D
blind and through hole with coolant with coolant with coolant with coolant
GT40_GP6520 GT41_GP6520 259/659 VDS401A WU25PD VDS402A WU25PD
— — — VDS401A02500 VDS402A02500
GT405001 GT415001 TCM25903300 VDS401A03300 VDS402A03300
— — — VDS401A03734 VDS402A03734
— — — VDS401A04039 VDS402A04039
GT405002 GT415002 TCM25904200 VDS401A04200 VDS402A04200
GT405003 GT415003 TCM25905000 VDS401A05000 VDS402A05000
— — TCM25905100 VDS401A05106 VDS402A05106
— — TCM25905400 VDS401A05410 VDS402A05410
— — TCM25906500 VDS401A06528 VDS402A06528
GT405004 GT415004 TCM25906700 VDS411A06700 VDS412A06700
— — TCM25906900 VDS411A06906 VDS412A06906
— — TCM65908000 VDS411A07938 VDS412A07938
— — — VDS411A08433 VDS412A08433
GT405005 GT415005 TCM25908500 VDS411A08500 VDS412A08500
— — TCM25909100 VDS411A09093 VDS412A09093
— — TCM25909900 VDS411A09921 VDS412A09921
GT405006 GT415006 TCM25910200 VDS411A10200 VDS412A10200
— — TCM65910500 VDS411A10716 VDS412A10716
— — TCM65911500 VDS411A11509 VDS412A11509
GT405007 GT415007 TCM25912000 VDS411A12000 VDS412A12000
— — TCM25913500 VDS411A13495 VDS412A13495
GT405008 GT415008 TCM25914000 VDS411A14000 VDS412A14000
GT405009 GT415009 TCM25915500 VDS411A15500 VDS412A15500
— — — VDS411A16670 VDS412A16670
GT405010 GT415010 TCM25917500 VDS411A17500 VDS412A17500
GT405011 — TCM25919500 VDS411A19500 VDS412A19500
Holemaking • High-Performance Taps
Recommended SC Drill
N
approximately 5 x D approximately 3 x D approximately 5 x D
with coolant with coolant with coolant
259/659 VDS401A WU25PD VDS401A WU25PD
— VDS401A02800 VDS402A02800
— VDS401A03734 VDS402A03734
TCM25904700 VDS401A04700 VDS402A04700
TCM25905600 VDS401A05600 VDS402A05600
TCM25907400 VDS411A07400 VDS412A07400
TCM25907600 VDS411A07600 VDS412A07600
TCM25909400 VDS411A09400 VDS412A09400
TCM25909500 VDS411A09500 VDS412A09500
TCM25909500 VDS411A09500 VDS412A09500
TCM25911300 VDS411A11300 VDS412A11300
TCM25911300 VDS411A11300 VDS412A11300
TCM25911500 VDS411A11500 VDS412A11500
— VDS411A13400 VDS412A13400
— VDS411A15200 VDS412A15200
— VDS411A15400 VDS412A15400
All Materials
Alternate Tap Drill
WWW.WIDIA.COM
A81
Page 81
High-Performance Taps
Cross Reference Chart • HSS-E-PM and Carbide Taps and Drills
High-Temperature Alloys
HSS-E-PM Taps —
Titanium Alloys
S
HSS-E-PM Taps —
Nickel and Cobalt Alloys
typical
thread sizes
metric mm inch GT16_WN35MG GT14_WN35MG GT12_WS32MG
M3 x 0,50 2,500 .0984 GT165001 GT145001 GT125001
M4 x 0,70 3,300 .1299 GT165002 GT145002 GT125002
M5 x 0,80 4,200 .1654 GT165003 GT145003 GT125003
M6 x 1,00 5,000 .1969 GT165004 GT145004 GT125004
M8 x 1,25 6,700 .2638 GT165005 GT145005 GT125005
M10 x 1,50 8,500 .3346 GT165006 GT145006 GT125006
M12 x 1,75 10,200 .4016 GT165007 GT145007 GT125007
M14 x 2,00 12,000 .4724 — — GT125008
Holemaking • High-Performance Taps
M16 x 2,00 14,000 .5512 — — GT125009
M20 x 2,50 17,500 .6890 — — GT125010
Hard Material
required
tap drill diameter
DIN 371, 374, 376
blind hole through hole blind hole
HSS-E-PM Taps — 44–55 HRC
H
HSS-E-PM Taps — 55–63 HRC
DIN 371, 374, 376
typical
thread sizes
metric mm inch GT06_WS32MG GX10_WH16PG
M3 x 0,50 2,500 .0984 — GX105001
M4 x 0,70 3,300 .1299 — GX105002
M5 x 0,80 4,200 .1654 — GX105003
M6 x 1,00 5,000 .1969 GT065003 GX105004
M8 x 1,25 6,700 .2638 GT065001 GX105005
M8 x 1,00 7,000 .2756 GT065006 GX105009
M10 x 1,50 8,500 .3346 GT065002 GX105007
M10 x 1,00 9,000 .3543 GT065007 GX105010
M12 x 1,75 10,200 .4016 GT065004 GX105007
M12 x 1,50 10,500 .4134 GT065008 GX105011
M14 x 2,00 12,000 .4724 — GX105008
M14 x 1,50 12,500 .4921 GT065009 GX105012
M16 x 2,00 14,000 .5512 GT065005 —
M16 x 1,50 14,500 .5709 GT065010 GX105013
required
tap drill diameter
blind and through hole blind and through hole
DIN 371, 374, 376
A82
WWW.WIDIA.COM
Page 82
High-Performance Taps
Cross Reference Chart • HSS-E-PM and Carbide Taps and Drills
HSS-E-PM Taps —
Nickel and Cobalt Alloys
S
Recommended SC Drill
All Materials
Alternate Tap Drill
DIN 371, 374, 376
approximately 3 x D approximately 5 x D approximately 3 x D approximately 5 x D
through hole with coolant with coolant with coolant with coolant
GT10_WS32MG WD 412522 WD 412527 TDS+ TDS+5
GT105001 — — VDS401A02500 VDS402A02500
GT105002 412522-000330 412527-000330 17050103300 17050203300
GT105003 412522-000420 412527-000420 17050104200 17050204200
GT105004 412522-000500 412527-000500 17050105000 17050205000
GT105005 412522-000670 412527-000670 17050106700 17050206700
GT105006 412522-000850 412527-000850 17050108500 17050208500
GT105007 412522-001020 412527-001020 17050110200 17050210200
GT105008 412522-001200 412527-001200 17050112000 17050212000
GT105009 412522-001400 412527-001400 17050114000 17050214000
GT105010 412522-001750 412527-001750 17050117500 17050217500
Holemaking • High-Performance Taps
Recommended SC Drill
approximately 3 x D approximately 5 x D approximately 3 x D approximately 5 x D
with coolant with coolant with coolant with coolant
™
WIDIA-Hanita
WIDIA-Hanita M155 custom solution
(special drill for hard materials)
M155 WIDIA-Hanita™M155 TDS+ TDS+
H
WIDIA-Hanita M155 custom solution
(special drill for hard materials)
All Materials
Alternative Tap Drill
— —
— —
17050104200 17050204200
17050105000 17050205000
17050106700 17050206700
17050107000 17050207000
17050108500 17050208500
17050109000 17050209000
17050110200 17050210200
17050110500 17050210500
17050112000 17050212000
17050112500 17050212500
17050114000 17050214000
17050114500 17050214500
WWW.WIDIA.COM
A83
Page 83
High-Performance Taps
Cross Reference Chart • HSS-E-PM Wind Energy Taps and Drills
Steel • Selector
typical
thread sizes
cutting taps
metric mm inch GT30_GP6520 GT50_GP6520 GT20_GP6520
M24 x 3,00 21,000 .8268 GT305161 GT505001 GT505111
M30 x 3,50 26,500 1.0433 GT305163 GT505002 GT505113
M33 x 3,50 29,500 1.1614 GT305164 GT505003 GT505114
M36 x 4,00 32,000 1.2598 GT305166 GT505004 GT505116
M42 x 4,50 37,500 1.4764 GT305168 GT505005 GT505118
required
tap drill diameter
Steel • Extra Long • Selector
Holemaking • High-Performance Taps
typical
thread sizes
cutting taps
metric mm inch GT30_GP6520 GT50_GP6520 GT20_GP6520
M24 x 3,00 21,000 .8268 GT305151 GT505006 GT205122
M30 x 3,50 26,500 1.0433 GT305153 GT505007 GT205124
M33 x 3,50 29,500 1.1614 GT305154 GT505008 GT205125
M36 x 4,00 32,000 1.2598 GT305156 GT505009 GT205127
M42 x 4,50 37,500 1.4764 GT305158 GT505010 GT205129
required
tap drill diameter
P
HSS-E-PM Taps
blind hole blind hole through hole
P
HSS-E-PM Taps
blind hole blind hole through hole
Cast Iron • Selector
K
HSS-E-PM Taps
typical
thread sizes
cutting taps
metric mm inch GT30_GP6520 GT50_GP6520 GT20_GP6520
M24 x 3,00 21,000 .8268 GT305161 GT505001 GT505111
M30 x 3,50 26,500 1.0433 GT305163 GT505002 GT505113
M33 x 3,50 29,500 1.1614 GT305164 GT505003 GT505114
M36 x 4,00 32,000 1.2598 GT305166 GT505004 GT505116
M42 x 4,50 37,500 1.4764 GT305168 GT505005 GT505118
required
tap drill diameter
blind hole blind hole through hole
Cast Iron • Extra Long • Selector
K
HSS-E-PM Taps
typical
thread sizes
cutting taps
metric mm inch GT30_GP6520 GT50_GP6520 GT20_GP6520
M24 x 3,00 21,000 .8268 GT305151 GT505006 GT205122
M30 x 3,50 26,500 1.0433 GT305153 GT505007 GT205124
M33 x 3,50 29,500 1.1614 GT305154 GT505008 GT205125
M36 x 4,00 32,000 1.2598 GT305156 GT505009 GT205127
M42 x 4,50 37,500 1.4764 GT305158 GT505010 GT205129
required
tap drill diameter
blind hole blind hole through hole
A84
WWW.WIDIA.COM
Page 84
High-Performance Taps
Cross Reference Chart • HSS-E-PM Wind Energy Taps and Drills
P
HSS-E-PM Taps
blind hole blind hole
Recommended Modular Drill
P
TOP DRILL
™
M1
with coolant with coolant tool body
GT31_GP6520 GT51_GP6520 insert 3 x D
GT315025 GT515001 TDM2100UPM TDM210R3SCF25M
GT315027 GT515002
GT315028 GT515003
GT315030 GT515004
Top Cut Plus™TN7015/XOMT-34 or
WIDIA-Metcut
™
Spade Blade Program
GT315032 GT515005
P
HSS-E-PM Taps
blind hole blind hole
Recommended Modular Drill
P
TOP DRILL
™
M1
with coolant with coolant tool body
GT31_GP6520 GT51_GP6520 insert 3 x D
GT315014 GT515006 TDM2100UPM TDM210R3SCF25M
GT315016 GT515007
GT315017 GT515008
GT315019 GT515009
Top Cut Plus™TN7015/XOMT-34 or
WIDIA-Metcut
™
Spade Blade Program
GT315021 GT515010
Holemaking • High-Performance Taps
HSS-E-PM Taps
K
blind hole blind hole
Recommended Modular Drill
K
TOP DRILL
™
M1
with coolant with coolant tool body
GT31_GP6520 GT51_GP6520 insert 3 x D
GT315025 GT515001 TDM2100UPM TDM210R3SCF25M
GT315027 GT515002
GT315028 GT515003
GT315030 GT515004
Top Cut Plus™TN5515/XOMT-35 or
WIDIA-Metcut
™
Spade Blade Program
GT315032 GT515005
K
HSS-E-PM Taps
blind hole blind hole
Recommended Modular Drill
K
TOP DRILL
™
M1
with coolant with coolant tool body
GT31_GP6520 GT51_GP6520 insert 3 x D
GT315014 GT515006 TDM2100UPM TDM210R3SCF25M
GT315016 GT515007
GT315017 GT515008
GT315019 GT515009
Top Cut Plus™TN5515/XOMT-35 or
WIDIA-Metcut
™
Spade Blade Program
GT315021 GT515010
WWW.WIDIA.COM
A85
Page 85
High-Performance HSS-E Taps
Our family of Exotic Material (EM) taps are specially designed to thread a
broad assortment of materials for unrivaled high-performance tapping.
WIDIA-GTD
• Enhanced tool geometry.
• Less tapping torque.
• Better chip removal.
™
A86
WWW.WIDIA.COM
Page 86
Unmatched Performance
The WIDIA-GTD™EM Series taps are designed and manufactured to
successfully thread high- and low-volume applications in aluminum,
stainless steel, nickel alloys, titanium alloys, mold steels, irons, brass,
bronze, and plastics. The formulation of premium steel tap base material
is unique for every application. The combination of a special geometry,
tap surface treatment, and premium steep gives these taps the highest
level of performance.
Premium Steels
EM Series taps use special HSS-E compositions containing chromium,
tungsten, molybdenum, vanadium, and cobalt, depending on the
application. The right combination improves tap performance resulting
in improved product finish and pitch diameter size. These taps have
excellent abrasion resistance and are designed for both high and low
volume production. Each tap maintains the same quality from the
first hole to the very last.
Broad Offering of Diameter Limits
Pitch diameters from H2–H7 and metric pitch diameters from D3–D7 are
stocked as standards in many styles, at no premium in price. With rigid
setups, higher pitch diameter limits can be used for longer tool life.
The EM Series offers many size options to produce the class of
thread desired.
WWW.WIDIA.COM
A87
Page 87
High-Performance Taps
Taps Selection Guide • EM HSS-E Taps
EM Series HP HSS-E Taps • ANSI Inch and Metric
Good
多
Better
多多
Best
多多多
EM Series High-Performance HSS-E Taps series
Holemaking • High-Performance Taps
EM-SS™GUN™- 8301
EM-SS™GUN™- 8351
EM-SS™GUN™6" -
8701
EM-SS™SPIRAL -
8304
EM-SS™SPIRAL -
8304
EM-SS™SPIRAL -
8354
EM-SS™SPIRAL -
8354
EM-SS™SPIRAL 6" -
8314
EM-SS™PIPE - 8321
size range
(inch and metric)
size
min - max
#2 - 2 4 1/2"
M3 - M18
#2 - 1/2" SH50 oxide extend 6"
#2 - 2 4 1/2"
#4 - 3/4" SH50 oxide ANSI 302A
M3 - M18
M3 - M18 SH50 oxide ANSI 302A
#2 - 1/2" SH50 oxide extend 6"
1/16" – 1 11 1/2" TiN, SH50 oxide, uncoated
hole
chamfer
form
3–5
3–5
3–5
coolant coating
TiCN,TiN,SH50 oxide,
uncoated
TiCN,TiN,SH50 oxide,
uncoated
TiCN,TiN,SH50 oxide,
uncoated
TiCN,TiN,SH50 oxide,
uncoated
tap
dimension
ANSI 302A
ANSI 302A
ANSI 302A
ANSI 302A
EM-AL GUN™- 8201
EM-AL GUN™- 8251
EM-ALS 25°
SPIRAL - 8204
EM-ALS 25°
SPIRAL - 8254
EM-AL 45º
SPIRAL - 8214
EM-AL 45º
SPIRAL - 8264
EM-NI™GUN™- 8601
EM-NI™GUN™- 8651
EM-NI™SPIRAL -
8604
EM-NI™SPIRAL -
8604
EM-NI™SPIRAL -
8654
EM-TI™LHSF - 8901
EM-TI™LHSF - 8951
#2 - 1/2" maxi-nitrite ANSI-DIN length
M3 - M12 maxi-nitrite ANSI-DIN length
#2 - 1/2" maxi-nitrite ANSI-DIN length
M3 - M12 maxi-nitrite ANSI-DIN length
#2 - 1/2" maxi-nitrite ANSI-DIN length
M3 - M12 maxi-nitrite ANSI-DIN length
#2 - 3/4"
M2,5 - M12 TiCN, SH47 oxide nitrite ANSI 302A
#2 - 3/4" TiCN, SH47 oxide nitrite ANSI 302A
#4 - 3/4" SH47 oxide nitrite ANSI 302A
M2,5 - M12 TiCN, SH47 oxide nitrite ANSI 302A
#2 - 1/2" maxi-nitrite ANSI 302A
M2,5 - M12 maxi-nitrite ANSI 302A
3–5
3–5
TiCN, SH47 oxide nitrite,
uncoated
ANSI 302A
A88
WWW.WIDIA.COM
Page 88
High-Performance Taps
Taps Selection Guide • EM HSS-E Taps
P M K N S H
1, 2, 3,
<35 HRC
4, 6, 7
Steel
5, 9,
10, 11
Steel
36–48
HRC
12, 13.1 13.2
PH &
Steel
PH &
Ferriitic
Stainless
Steel
>35 HRC
Ferriitic
Stainless
<35 HRC
14.1, 14.2,
14.3, 14.4
Stainless
Steel
15, 16,
17, 18, 19
Cast Iron
20 21
Wrought
Aluminum
22, 23,
24, 25
Cast
Aluminum
26, 27,
28
Copper,
Copper
Alloys
多多多 多 多多 多多 多多
多多多 多 多多 多多 多多
多多多 多 多多 多多
多多多 多 多多 多多 多多
多多多 多 多多 多多
多多多 多 多多 多多 多多
多多多 多 多多 多多
多多多 多 多多 多多
多多多 多 多多 多多 多多 多多
多多多 多多 多多
多多多 多多 多多
多多 多多多 多多
多多 多多多 多多
多多多 多多 多多
多多多 多多 多多
多 多 多 多 多多多
多 多 多 多 多多多
多 多 多 多 多多多
多 多 多 多 多多多
多 多 多 多 多多多
多 多多多
多 多多多
31, 32
Iron
Based
33, 34,
35
Cobalt
Based
36 37
Nickel
Based
Titanium
& Alloys
38.1, 38.2,
40.1, 40.2,
41.1
Hardened
Steel
49–55
HRC
39.1,
41.2
Hardened
Steel
56–68
HRC
Recommended
Page(s)
Cutting
Parameters
A92–
A264–A265
A94
A95 A264–A265
A96 A264–A265
A97–
A264–A265
A99
A100–
A264–A265
A101
A102 A264–A265
A103 A264–A265
A104 A264–A265
A105 A264–A265
A106 A264–A265
A107 A264–A265
A108 A264–A265
A109 A264–A265
A110 A264–A265
A111 A264–A265
A112–
A264–A265
A113
A114 A264–A265
A115–
A264–A265
A116
A117–
A264–A265
A118
A119 A264–A265
A120 A264–A265
A121 A264–A265
Holemaking • High-Performance Taps
WWW.WIDIA.COM
(continued )
A89
Page 89
High-Performance Taps
Taps Selection Guide • EM HSS-E Taps
(continued)
EM Series HP HSS-E Taps • ANSI Inch and Metric
Good
多
Better
多多
Best
多多多
EM Series High-Performance HSS-E Taps series
Holemaking • High-Performance Taps
EM-TI™SPIRAL -
8904
EM-TI™SPIRAL -
8904
EM-TI™SPIRAL -
8954
EM-MS™MOLD -
8330
EM-MS™MOLD PIPE -
8320
Solid Carbide - 8603
size range
(inch and metric)
size
min - max
#2 - 1/2" maxi-nitrite ANSI 302A
#4 - 1/2" maxi-nitrite ANSI 302A
M2,5 - M12 maxi-nitrite ANSI 302A
#4 - 3/4" uncoated ANSI 302A
1/8 - 3/4 uncoated
#10 - 5/8" uncoated ANSI 302A
hole
chamfer
form
4–6
coolant coating
tap
dimension
EM Series High-Performance
HSS-E Forming Taps
Solid Carbide - 8653
Solid Carbide - 8603
Solid Carbide - 8653
Solid Carbide - 8703
Solid Carbide - 8753
Solid Carbide - 8703
Solid Carbide - 8753
EM-TLD - 8580
EM-TLD - 8590
EM-TL - 8502
EM-TL - 8512
EM-TL - 8500
EM-TL - 8510
M3 - M16 uncoated ANSI 302A
#10 - 5/8" uncoated ANSI 302A
M3 - M16 uncoated ANSI 302A
#5 - 1/2" uncoated ANSI 302A
M3 - M12 uncoated ANSI 302A
#5 - 1/2" uncoated ANSI 302A
M3 - M12 uncoated ANSI 302A
#2 - 1/4" TiCN ANSI-DIN length
M3 - M6 TiCN ANSI-DIN length
#0 - 2/4" TiCN ANSI-DIN length
M3 - M12 TiCN ANSI-DIN length
#6 - 1/2" TiCN ANSI-DIN length
M3 - M12 TiCN ANSI-DIN length
3–5
3–5
A90
WWW.WIDIA.COM
Page 90
High-Performance Taps
Taps Selection Guide • EM HSS-E Taps
P M K N S H
1, 2, 3,
4, 6, 7
Steel
<35 HRC
5, 9,
10, 11
Steel
36–48
HRC
12, 13.1 13.2
PH &
Ferriitic
Stainless
Steel
<35 HRC
PH &
Ferriitic
Stainless
Steel
>35 HRC
14.1, 14.2,
14.3, 14.4
Stainless
Steel
15, 16,
17, 18, 19
Cast Iron
20 21
Wrought
Aluminum
22, 23,
24, 25
Aluminum
多多 多多 多
多多 多多 多
多多多
多多多
多多多
多多多
多多多
多多多
多多多
多多多
Cast
26, 27,
28
Copper,
Copper
Alloys
31, 32
Iron
Based
33, 34,
35
Cobalt
Based
多 多多多
多 多多多
多 多多多
36 37
Nickel
Based
Titanium
& Alloys
38.1, 38.2,
40.1, 40.2,
41.1
Hardened
Steel
49–55
HRC
39.1,
41.2
Hardened
Steel
56–68
HRC
Recommended
Page
Cutting
Parameters
A122 A264–A265
A123 A264–A265
A124 A264–A265
A125 A264–A265
A126 A264–A265
A127 A264–A265
A129 A264–A265
A128 A264–A265
A130 A264–A265
A131 A264–A265
A133 A264–A265
A132 A264–A265
A134 A264–A265
Holemaking • High-Performance Taps
多多多
多多多 多 多 多
多多多 多 多 多
多多多 多 多 多
多多多 多 多 多
多多多 多 多 多
多多多 多 多 多
A135 A264–A265
A136 A264–A265
A137 A264–A265
A138 A264–A265
A139 A264–A265
A140 A264–A265
WWW.WIDIA.COM
A91
Page 91
High-Performance Taps
EM-SS GUN™Taps • Through Holes
Series 8301 • Machine Screw and Fractional • Plug Chamfer
Holemaking • High-Performance Taps
3–5
䢇
first choice
嘷
alternate choice
TiCN TiN oxide uncoated D1 size L L3 L2 D
— — 82623 — 2 - 56 1.75 .26 .44 .141 2 H2
— — 82624 — 2 - 56 1.75 .26 .44 .141 2 H3
— — 82636 — 2 - 56 1.75 .26 .44 .141 2 H4
— — 82600 — 3 - 48 1.81 .30 .50 .141 2 H2
82301 82901 82601 82601B 4 - 40 1.88 .34 .56 .141 2 H2
— — 82602 — 4 - 40 1.88 .34 .56 .141 2 H3
— — 82612 — 4 - 40 1.88 .34 .56 .141 2 H4
— — 82634 82634B 4 - 40 1.88 .34 .56 .141 2 H5
— — 82638 — 4 - 40 1.88 .34 .56 .141 2 H6
— — 82683 — 4 - 48 1.88 .34 .56 .141 2 H2
— — 82641 — 4 - 48 1.88 .34 .56 .141 2 H4
— — 82603 — 5 - 40 1.94 .37 .63 .141 3 H2
— — 82604 — 6 - 32 2.00 .41 .69 .141 3 H2
82305 82905 82605 82605B 6 - 32 2.00 .41 .69 .141 3 H3
— — 82608 — 6 - 32 2.00 .41 .69 .141 3 H4
— — 82635 82635B 6 - 32 2.00 .41 .69 .141 3 H5
— — 82659 6 - 32 2.00 .41 .69 .141 3 H6
— — 82665 82665B 6 - 32 2.00 .41 .69 .141 3 H7
— — 82684 — 6 - 40 2.00 .41 .69 .141 3 H2
— — 82642 — 6 - 40 2.00 .41 .69 .141 3 H3
82606 — 8 - 32 2.13 .45 .75 .168 3 H2
82307 82907 82607 82607B 8 - 32 2.13 .45 .75 .168 3 H3
— — 82629 — 8 - 32 2.13 .45 .75 .168 3 H4
— — 82637 82637B 8 - 32 2.13 .45 .75 .168 3 H5
— — 82660 — 8 - 32 2.13 .45 .75 .168 3 H6
— — 82667 — 8 - 32 2.13 .45 .75 .168 3 H7
— 82686 — 8 - 36 2.13 .45 .75 .168 3 H2
82309 82909 82609 82609B 10 - 24 2.38 .53 .88 .194 3 H3
— — 82657 — 10 - 24 2.38 .53 .88 .194 3 H4
— — 82639 82639B 10 - 24 2.38 .53 .88 .194 3 H5
— — 82690 — 10 - 24 2.38 .53 .88 .194 3 H6
— — 82669 — 10 - 24 2.38 .53 .88 .194 3 H7
82611 — 10 - 32 2.38 .53 .88 .194 3 H2
82310 82910 82610 82610B 10 - 32 2.38 .53 .88 .194 3 H3
— — 82630 — 10 - 32 2.38 .53 .88 .194 3 H4
— — 82640 82640B 10 - 32 2.38 .53 .88 .194 3 H5
— — 82661 — 10 - 32 2.38 .53 .88 .194 3 H6
— — 82670 — 10 - 32 2.38 .53 .88 .194 3 H7
number
of flutes
pitch diameter
limit
(continued)
A92
WWW.WIDIA.COM
Page 92
(Series 8301 • Machine Screw and Fractional • Plug Chamfer continued)
High-Performance Taps
EM-SS GUN™Taps • Through Holes
TiCN TiN oxide uncoated D1 size L L3 L2 D
— — 82688 — 12 - 24 2.38 .57 .94 .220 3 H3
— — 82689 — 12 - 28 2.38 .57 .94 .220 3 H3
— — 82658 — 1/4 - 20 2.50 .59 1.00 .255 3 H2
82313 82913 82613 82613B 1/4 - 20 2.50 .59 1.00 .255 3 H3
— — 82643 82643B 1/4 - 20 2.50 .59 1.00 .255 3 H5
— — 82673 — 1/4 - 20 2.50 .59 1.00 .255 3 H7
— — 82666 — 1/4 - 28 2.50 .59 1.00 .255 3 H2
82314 82914 82614 82614B 1/4 - 28 2.50 .59 1.00 .255 3 H3
— — 82631 — 1/4 - 28 2.50 .59 1.00 .255 3 H4
— — 82644 82644B 1/4 - 28 2.50 .59 1.00 .255 3 H5
— — 82662 — 1/4 - 28 2.50 .59 1.00 .255 3 H6
— — 82674 — 1/4 - 28 2.50 .59 1.00 .255 3 H7
82315 82915 82615 82615B 5/16 - 18 2.72 .67 1.13 .318 3 H3
— — 82645 82645B 5/16 - 18 2.72 .67 1.13 .318 3 H5
— — 82675 — 5/16 - 18 2.72 .67 1.13 .318 3 H7
82316 82916 82616 82616B 5/16 - 24 2.72 .67 1.13 .318 3 H3
— — 82632 — 5/16 - 24 2.72 .67 1.13 .318 3 H4
— — 82646 82646B 5/16 - 24 2.72 .67 1.13 .318 3 H5
— — 82663 — 5/16 - 24 2.72 .67 1.13 .318 3 H6
— — 82676 — 5/16 - 24 2.72 .67 1.13 .318 3 H7
82317 82917 82617 82617B 3/8 - 16 2.94 .75 1.25 .381 3 H3
— — 82647 82647B 3/8 - 16 2.94 .75 1.25 .381 3 H5
— — 82668 — 3/8 - 16 2.94 .75 1.25 .381 3 H7
82318 82918 82618 82618B 3/8 - 24 2.94 .75 1.25 .381 3 H3
— — 82633 — 3/8 - 24 2.94 .75 1.25 .381 3 H4
— — 82648 82648B 3/8 - 24 2.94 .75 1.25 .381 3 H5
— — 82664 — 3/8 - 24 2.94 .75 1.25 .381 3 H6
— — 82678 — 3/8 - 24 2.94 .75 1.25 .381 3 H7
82319 82919 82619 82619B 7/16 - 14 3.16 .89 — .323 3 H3
— — 82649 82649B 7/16 - 14 3.16 .89 — .323 3 H5
— — 82671 — 7/16 - 14 3.16 .89 — .323 3 H7
82320 82920 82620 82620B 7/16 - 20 3.16 .89 — .323 3 H3
— — 82650 82650B 7/16 - 20 3.16 .89 — .323 3 H5
— — 82691 — 7/16 - 20 3.16 .89 — .323 3 H6
— — 82680 — 7/16 - 20 3.16 .89 — .323 3 H7
82321 82921 82621 82621B 1/2 - 13 3.38 .98 — .367 3 H3
— — 82651 82651B 1/2 - 13 3.38 .98 — .367 3 H5
— — 82681 — 1/2 - 13 3.38 .98 — .367 3 H7
82322 82922 82622 82622B 1/2 - 20 3.38 .98 — .367 3 H3
— — 82652 82652B 1/2 - 20 3.38 .98 — .367 3 H5
— — 82692 — 1/2 - 20 3.38 .98 — .367 3 H6
— — 82682 — 1/2 - 20 3.38 .98 — .367 3 H7
number
of flutes
pitch diameter
limit
(continued)
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A93
Page 93
High-Performance Taps
EM-SS GUN™Taps •Through Holes
(Series 8301 • Machine Screw and Fractional • Plug Chamfer continued)
TiCN TiN oxide uncoated D1 size L L3 L2 D
82353 82953 82653 82653B 9/16 - 12 3.59 .98 — .429 3 H3
82354 82954 82654 82654B 9/16 - 18 3.59 .98 — .429 3 H3
82325 82925 82625 82625B 5/8 - 11 3.81 1.08 — .480 3 H3
— — 82655 82655B 5/8 - 11 3.81 1.08 — .480 3 H5
— — 82672 — 5/8 - 11 3.81 1.08 — .480 3 H7
82326 82926 82626 82626B 5/8 - 18 3.81 1.08 — .480 3 H3
— — 82656 82656B 5/8 - 18 3.81 1.08 — .480 3 H5
— — 82694 — 5/8 - 18 3.81 1.08 — .480 3 H6
Holemaking • High-Performance Taps
EM taps for 3B class of fit are suitable for UNJ aerospace internal threading applications.
Refer to table on pages A257–A258 for the recommended pitch diameter limit for 2B or 3B class of fit.
— — 82677 — 5/8 - 18 3.81 1.08 — .480 3 H7
82327 82927 82627 82627B 3/4 - 10 4.25 1.20 — .590 3 H3
— — 81657 — 3/4 - 10 4.25 1.20 — .590 3 H5
82328 82928 82628 82628B 3/4 - 16 4.25 1.20 — .590 3 H3
82395 82995 82695 82695B 7/8 - 9 4.69 1.34 — .697 3 H4
82396 82996 82696 82696B 7/8 - 14 4.69 1.34 — .697 3 H4
82397 82997 82697 82697B 1 - 8 5.13 1.50 — .800 3 H4
— — 82679 — 1 - 12 5.13 1.50 — .800 3 H4
— — — 82700 1 1/8 - 7 5.44 2.56 — .896 4 H6
— — — 82701 1 1/8 - 12 5.44 2.56 — .896 4 H5
— — — 82702 1 1/4 - 7 5.75 2.56 — 1.021 4 H6
— — — 82703 1 1/4 - 12 5.75 2.56 — 1.021 4 H5
— — — 82705 1 3/8 - 6 6.06 3.00 — 1.108 4 H6
— — — 82706 1 3/8 - 12 6.06 3.00 — 1.108 4 H5
— — — 82707 1 1/2 - 6 6.38 3.00 — 1.233 4 H6
— — — 82708 1 1/2 - 12 6.38 3.00 — 1.233 4 H5
— — — 82709 1 3/4 - 5 7.00 3.19 — 1.430 4 H7
— — — 82710 2 - 4 1/2 7.63 3.56 — 1.644 4 H7
number
of flutes
pitch diameter
limit
A94
WWW.WIDIA.COM
Page 94
High-Performance Taps
EM-SS Metric GUN™Taps for Through Holes
3–5
䢇
first choice
嘷
alternate choice
Series 8351 • Plug Chamfer • Metric ANSI
TiCN TiN oxide uncoated D1 size L L3 L2 D
72815 72915 72615 72615B M3 X 0,5 1.94 .31 .63 .141 3 D3
— — 72616 72616B M3,5 X 0,6 2.00 .38 .69 .141 3 D4
72817 72917 72617 72617B M4 X 0,7 2.13 .38 .75 .168 3 D4
72819 72919 72619 72619B M5 X 0,8 2.38 .50 .88 .194 3 D4
72820 72920 72620 72620B M6 X 1 2.50 .63 1.00 .255 3 D5
— — 72621 72621B M7 X 1 2.72 .69 1.13 .318 3 D5
— — 72622 72622B M8 X 1 2.72 .69 1.13 .318 3 D5
72823 72923 72623 72623B M8 X 1,25 2.72 .69 1.13 .318 3 D5
— — 72624 72624B M10 X 1,25 2.94 .75 1.25 .381 3 D5
72825 72925 72625 72625B M10 X 1,5 2.94 .75 1.25 .381 3 D6
— — 72626 72626B M12 X 1,25 3.38 .94 — .367 3 D5
72827 72927 72627 72627B M12 X 1,75 3.38 .94 — .367 3 D6
— — 72628 72628B M14 X 1,5 3.59 1.00 — .429 3 D6
— — 72629 72629B M14 X 2 3.59 1.00 — .429 3 D7
— — 72630 72630B M16 X 1,5 3.81 1.09 — .480 3 D6
— 72930 — — M16 X 1,5 3.81 1.09 — .480 — D6
— — 72631 — M16 X 2 3.81 1.09 — .480 3 D7
72831 72931 — — M16 X 2 3.81 1.09 — .480 3 D7
— — — 72631B M16 X 2 3.81 1.09 — .480 3 D7
— — 72632 — M18 X 1,5 4.03 1.09 — .542 3 D6
— — — 72632B M18 X 1,5 4.03 1.08 — .542 4 D6
— — 1072633 — M18 X 2,5 4.03 1.08 — .542 3 D7
— — — 72633B M18 X 2,5 4.03 1.08 — .542 4 D7
Metric taps for 6H class of fit are suitable for MJ aerospace internal threading applications.
Metric taps are manufactured to USCTI specifications and dimensions.
Metric tap blank dimensions are equivalent to inch taps.
Refer to table on pages A257–A258 for the recommended pitch diameter limit for 6H class of fit.
number
of flutes
ANSI
M
pitch diameter
limit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A95
Page 95
High-Performance Taps
EM-SS Extended Shank GUN™Taps • Through Holes • 6" Length
Series 8701 • Machine Screw and Fractional • Plug Chamfer
Holemaking • High-Performance Taps
3–5
䢇
first choice
嘷
alternate choice
oxide D1 size L L3 L2 D
82523 2 - 56 6.00 .44 — .141 2 H2
82500 3 - 48 6.00 .50 — .141 2 H2
82501 4 - 40 6.00 .31 .56 .141 2 H2
82505 6 - 32 6.00 .38 .69 .141 3 H3
82507 8 - 32 6.00 .38 .75 .168 3 H3
82509 10 - 24 6.00 .50 .88 .194 3 H3
82510 10 - 32 6.00 .50 .88 .194 3 H3
82513 1/4 - 20 6.00 .63 1.00 .255 3 H3
82514 1/4 - 28 6.00 .63 1.00 .255 3 H3
82515 5/16 - 18 6.00 .69 1.13 .318 3 H3
82516 5/16 - 24 6.00 .69 1.13 .318 3 H3
82517 3/8 - 16 6.00 .75 1.25 .381 3 H3
82518 3/8 - 24 6.00 .75 1.25 .381 3 H3
82519 7/16 - 14 6.00 .88 — .323 3 H3
82520 7/16 - 20 6.00 .88 — .323 3 H3
82521 1/2 - 13 6.00 .94 — .367 3 H3
82522 1/2 - 20 6.00 .94 — .367 3 H3
EM taps for 3B class of fit are suitable for UNJ aerospace internal threading applications.
Refer to table on pages A257–A258 for the recommended pitch diameter limit for 2B or 3B class of fit.
number
of flutes
pitch diameter
limit
A96
WWW.WIDIA.COM
Page 96
EM-SS Spiral-Flute Taps •Blind Holes
Series 8304 • Machine Screw and Fractional • Chamfer 2-1/2–3-1/2 Pitches
High-Performance Taps
䢇
first choice
嘷
alternate choice
Holemaking • High-Performance Taps
TiCN TiN oxide uncoated D1 size L L3 L2 D
— — 84671 84671B 2 - 56 1.75 .44 — .141 2 H2
— — 84672 — 3 - 48 1.81 .50 — .141 2 H2
84301 84901 84601 84601B 4 - 40 1.88 .24 .56 .141 2 H2
— — 84602 — 4 - 40 1.88 .24 .56 .141 2 H3
— — 84629 — 4 - 40 1.88 .24 .56 .141 2 H4
— — 84634 84634B 4 - 40 1.88 .24 .56 .141 2 H5
— — 84612 — 4 - 40 1.88 .24 .56 .141 2 H6
— — 84683 — 4 - 48 1.88 .24 .56 .141 2 H2
84303 84903 84603 84603B 5 - 40 1.94 .24 .63 .141 3 H2
— — 84604 — 6 - 32 2.00 .28 .69 .141 3 H2
84305 84905 84605 84605B 6 - 32 2.00 .28 .69 .141 3 H3
— — 84636 — 6 - 32 2.00 .28 .69 .141 3 H4
— — 84635 84635B 6 - 32 2.00 .28 .69 .141 3 H5
— — 84665 — 6 - 32 2.00 .28 .69 .141 3 H7
— — 84684 — 6 - 40 2.00 .28 .69 .141 3 H2
— — 84685 — 6 - 40 2.00 .28 .69 .141 3 H3
— — 84606 — 8 - 32 2.13 .28 .75 .168 3 H2
84307 84907 84607 84607B 8 - 32 2.13 .28 .75 .168 3 H3
— — 84638 — 8 - 32 2.13 .28 .75 .168 3 H4
— — 84637 84637B 8 - 32 2.13 .28 .75 .168 3 H5
— — 84660 — 8 - 32 2.13 .28 .75 .168 3 H6
— — 84667 — 8 - 32 2.13 .28 .75 .168 3 H7
— — 84687 — 8 - 36 2.13 .28 .75 .168 3 H3
— — 84624 — 10 - 24 2.38 .35 .88 .194 3 H2
84309 84909 84609 84609B 10 - 24 2.38 .35 .88 .194 3 H3
— — 84623 — 10 - 24 2.38 .35 .88 .194 3 H4
— — 84639 84639B 10 - 24 2.38 .35 .88 .194 3 H5
— — 84669 — 10 - 24 2.38 .35 .88 .194 3 H7
— — 84611 — 10 - 32 2.38 .28 .88 .194 3 H2
84310 84910 84610 84610B 10 - 32 2.38 .28 .88 .194 3 H3
— — 84630 — 10 - 32 2.38 .28 .88 .194 3 H4
— — 84640 84640B 10 - 32 2.38 .28 .88 .194 3 H5
— — 84662 — 10 - 32 2.38 .28 .88 .194 3 H6
— — 84670 — 10 - 32 2.38 .28 .88 .194 3 H7
number
of flutes
pitch diameter
limit
(continued)
WWW.WIDIA.COM
A97
Page 97
High-Performance Taps
EM-SS Spiral-Flute Taps •Blind Holes
(Series 8304 • Machine Screw and Fractional • Chamfer 2-1/2–3-1/2 Pitches continued)
Holemaking • High-Performance Taps
TiCN TiN oxide uncoated D1 size L L3 L2 D
— — 84688 — 12 - 24 2.38 .35 .94 .220 3 H3
— — 84689 — 12 - 28 2.38 .28 .94 .220 3 H3
— — 84641 — 1/4 - 20 2.50 .43 1.00 .255 3 H2
84313 84913 84613 84613B 1/4 - 20 2.50 .43 1.00 .255 3 H3
— — 84643 84643B 1/4 - 20 2.50 .43 1.00 .255 3 H5
— — 84673 — 1/4 - 20 2.50 .43 1.00 .255 3 H7
— — 84642 — 1/4 - 28 2.50 .35 1.00 .255 3 H2
84314 84914 84614 84614B 1/4 - 28 2.50 .35 1.00 .255 3 H3
— — 84631 — 1/4 - 28 2.50 .35 1.00 .255 3 H4
— — 84644 84644B 1/4 - 28 2.50 .35 1.00 .255 3 H5
— — 84664 — 1/4 - 28 2.50 .35 1.00 .255 3 H6
— — 84674 — 1/4 - 28 2.50 .35 1.00 .255 3 H7
84315 84915 84615 84615B 5/16 - 18 2.72 .47 1.13 .318 3 H3
— — 84645 84645B 5/16 - 18 2.72 .47 1.13 .318 3 H5
— — 84675 — 5/16 - 18 2.72 .47 1.13 .318 3 H7
84316 84916 84616 84616B 5/16 - 24 2.72 .39 1.13 .318 3 H3
— — 84646 84646B 5/16 - 24 2.72 .39 1.13 .318 3 H5
— — 84657 — 5/16 - 24 2.72 .39 1.13 .318 3 H6
— — 84676 — 5/16 - 24 2.72 .39 1.13 .318 3 H7
84317 84917 84617 84617B 3/8 - 16 2.94 .55 1.25 .381 3 H3
— — 84647 84647B 3/8 - 16 2.94 .55 1.25 .381 3 H5
— — 84677 — 3/8 - 16 2.94 .55 1.25 .381 3 H7
84318 84918 84618 84618B 3/8 - 24 2.94 .39 1.25 .381 3 H3
— — 84633 — 3/8 - 24 2.94 .39 1.25 .381 3 H4
— — 84648 84648B 3/8 - 24 2.94 .39 1.25 .381 3 H5
— — 84658 — 3/8 - 24 2.94 .39 1.25 .381 3 H6
— — 84678 — 3/8 - 24 2.94 .39 1.25 .381 3 H7
84319 84919 84619 84619B 7/16 - 14 3.16 .59 — .323 3 H3
— — 84649 84649B 7/16 - 14 3.16 .59 — .323 3 H5
— — 84679 — 7/16 - 14 3.16 .59 — .323 3 H7
84320 84920 84620 84620B 7/16 - 20 3.16 .47 — .323 3 H3
— — 84650 84650B 7/16 - 20 3.16 .47 — .323 3 H5
— — 84691 — 7/16 - 20 3.16 .47 — .323 3 H6
— — 84680 — 7/16 - 20 3.16 .47 — .323 3 H7
84321 84921 84621 84621B 1/2 - 13 3.38 .63 — .367 3 H3
— — 84651 84651B 1/2 - 13 3.38 .63 — .367 3 H5
— — 84681 — 1/2 - 13 3.38 .63 — .367 3 H7
84322 84922 84622 84622B 1/2 - 20 3.38 .47 — .367 3 H3
— — 84652 84652B 1/2 - 20 3.38 .47 — .367 3 H5
— — 84692 — 1/2 - 20 3.38 .47 — .367 3 H6
— — 84682 — 1/2 - 20 3.38 .47 — .367 3 H7
84353 84953 84653 84653B 9/16 - 12 3.59 .71 — .429 3 H3
number
of flutes
pitch
diameter
limit
(continued)
A98
WWW.WIDIA.COM
Page 98
(Series 8304 • Machine Screw and Fractional • Chamfer 2-1/2–3-1/2 Pitches continued)
High-Performance Taps
EM-SS Spiral-Flute Taps •Blind Holes
TiCN TiN oxide uncoated D1 size L L3 L2 D
— — 84699 84699B 9/16 - 12 3.59 .71 — .429 3 H5
84354 84954 84654 84654B 9/16 - 18 3.59 .51 — .429 3 H3
— — 84698 84698B 9/16 - 18 3.59 .51 — .429 3 H5
84325 84925 84625 84625B 5/8 - 11 3.81 .75 — .480 3 H3
— — 84655 84655B 5/8 - 11 3.81 .75 — .480 3 H5
— — 84661 — 5/8 - 11 3.81 .75 — .480 3 H7
84326 84926 84626 84626B 5/8 - 18 3.81 .51 — .480 3 H3
— — 84656 84656B 5/8 - 18 3.81 .51 — .480 3 H5
— — 84663 — 5/8 - 18 3.81 .51 — .480 3 H6
— — 84666 — 5/8 - 18 3.81 .51 — .480 3 H7
84327 84927 84627 84627B 3/4 - 10 4.25 .83 — .590 4 H3
— — 84693 — 3/4 - 10 4.25 .83 — .590 4 H5
84328 84928 84628 84628B 3/4 - 16 4.25 .59 — .590 4 H3
— — 84694 — 3/4 - 16 4.25 .59 — .590 4 H5
— — 84686 — 3/4 - 16 4.25 .59 — .590 4 H7
84395 84995 84695 84695B 7/8 - 9 4.69 .83 — .697 4 H4
84396 84996 84696 84696B 7/8 - 14 4.69 .71 — .697 4 H4
84397 84997 84697 — 1 - 8 5.13 .98 — .800 4 H4
— — 84668 — 1 - 12 5.13 .71 — .800 4 H4
— — — 84701B 1 1/8 - 7 5.44 2.56 — .896 4 H6
— — — 84702 1 1/8 - 12 5.44 2.56 — .896 4 H5
— — — 84703B 1 1/4 - 7 5.75 2.56 — 1.021 4 H6
— — — 84705 1 1/4 - 12 5.75 2.56 — 1.021 4 H5
— — — 84706 1 3/8 - 6 6.06 3.00 — 1.108 4 H6
— — — 84707 1 3/8 - 12 6.06 3.00 — 1.108 4 H5
— — — 84709 1 1/2 - 6 6.38 3.00 — 1.233 4 H6
— — — 84711 1 1/2 - 12 6.38 3.00 — 1.233 4 H5
— — — 84714 1 3/4 - 5 7.00 3.19 — 1.430 4 H7
— — — 84715B 2 - 4 1/2 7.63 3.56 — 1.644 4 H3
— — — 84697B 1 - 8 5.13 .98 — .800 4 H4
EM taps for 3B class of fit are suitable for UNJ aerospace internal threading applications.
Refer to table on pages A257–A258 for the recommended pitch diameter limit for 2B or 3B class of fit.
number
of flutes
pitch
diameter
limit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A99
Page 99
High-Performance Taps
EM-SS Spiral-Flute Taps • Threading Close to the Bottom in a Blind Hole
Series 8304 • Machine Screw and Fractionl • Full Bottoming Chamfer
Holemaking • High-Performance Taps
䢇
first choice
嘷
alternate choice
oxide D1 size L L3 L2 D
84001 4 - 40 1.88 .24 .56 .141 2 H2
84002 4 - 40 1.88 .24 .56 .141 2 H3
84034 4 - 40 1.88 .24 .56 .141 2 H5
84083 4 - 48 1.88 .24 .56 .141 2 H2
84003 5 - 40 1.94 .24 .63 .141 3 H2
84004 6 - 32 2.00 .28 .69 .141 3 H2
84005 6 - 32 2.00 .28 .69 .141 3 H3
84035 6 - 32 2.00 .28 .69 .141 3 H5
84084 6 - 40 2.00 .28 .69 .141 3 H2
84085 6 - 40 2.00 .28 .69 .141 3 H3
84006 8 - 32 2.13 .28 .75 .168 3 H2
84007 8 - 32 2.13 .28 .75 .168 3 H3
84037 8 - 32 2.13 .28 .75 .168 3 H5
84009 10 - 24 2.38 .35 .88 .194 3 H3
84039 10 - 24 2.38 .35 .88 .194 3 H5
84010 10 - 32 2.38 .28 .88 .194 3 H3
84040 10 - 32 2.38 .28 .88 .194 3 H5
84013 1/4 - 20 2.50 .43 1.00 .255 3 H3
84043 1/4 - 20 2.50 .43 1.00 .255 3 H5
84014 1/4 - 28 2.50 .35 1.00 .255 3 H3
84044 1/4 - 28 2.50 .35 1.00 .255 3 H5
84015 5/16 - 18 2.72 .47 1.13 .318 3 H3
84045 5/16 - 18 2.72 .47 1.13 .318 3 H5
84016 5/16 - 24 2.72 .39 1.13 .318 3 H3
84046 5/16 - 24 2.72 .39 1.13 .318 3 H5
84017 3/8 - 16 2.94 .55 1.25 .381 3 H3
84047 3/8 - 16 2.94 .55 1.25 .381 3 H5
84077 3/8 - 16 2.94 .55 1.25 .381 3 H7
84018 3/8 - 24 2.94 .39 1.25 .381 3 H3
84033 3/8 - 24 2.94 .39 1.25 .381 3 H4
84048 3/8 - 24 2.94 .39 1.25 .381 3 H5
84019 7/16 - 14 3.16 .59 — .323 3 H3
84049 7/16 - 14 3.16 .59 — .323 3 H5
84020 7/16 - 20 3.16 .47 — .323 3 H3
number
of flutes
pitch diameter
limit
(continued)
A100
WWW.WIDIA.COM
Page 100
EM-SS Spiral-Flute Taps • Threading Close to the Bottom in a Blind Hole
(Series 8304 • Machine Screw and Fractionl • Full Bottoming Chamfer continued)
High-Performance Taps
oxide D1 size L L3 L2 D
84050 7/16 - 20 3.16 .47 — .323 3 H5
84021 1/2 - 13 3.38 .63 — .367 3 H3
84051 1/2 - 13 3.38 .63 — .367 3 H5
84022 1/2 - 20 3.38 .47 — .367 3 H3
84052 1/2 - 20 3.38 .47 — .367 3 H5
84053 9/16 - 12 3.59 .71 — .429 3 H3
84054 9/16 - 18 3.59 .51 — .429 3 H3
84025 5/8 - 11 3.81 .75 — .480 3 H3
84055 5/8 - 11 3.81 .75 — .480 3 H5
84026 5/8 - 18 3.81 .51 — .480 3 H3
84056 5/8 - 18 3.81 .51 — .480 3 H5
84027 3/4 - 10 4.25 .83 — .590 4 H3
84028 3/4 - 16 4.25 .59 — .590 4 H3
EM taps for 3B class of fit are suitable for UNJ aerospace internal threading applications.
Refer to table on pages A257–A258 for the recommended pitch diameter limit for 2B or 3B class of fit.
number
of flutes
pitch diameter
limit
Holemaking • High-Performance Taps
WWW.WIDIA.COM
A101
 Loading...