

Page 1

Electronic copies of the most current TSM issue can be found on the Viking Pump website at www.vikingpump.com
TECHNICAL SERVICE MANUAL
CONTENTS
Introduction 1
Special Information 2
Maintenance 2
Packed Pumps 4
Mechanical Seal Pumps 8
Optional PTFE Seal 12
Thrust Bearing Adjustment 13
Installation of Carbon Graphite Bushings 13
Pressure Relief Valve Instructions 14
Warranty 15
HEAVY DUTY PUMPS
SERIES 335 AND 4335
SIZES N, R, AND P
SECTION TSM 143
PAGE 1 OF 15
ISSUE E
FIGURE 1
INTRODUCTION
The illustrations used in this manual are for identification
purposes only and cannot be used for ordering parts. Obtain
a parts list from the factory or a Viking® representative.
Always give the complete name of the part, part number
and material with the model number and serial number of
the pump when ordering repair parts. The unmounted pump
or pump unit model number and serial number are on the
nameplate.
In the Viking model number system, basic size letters are
combined with the series number (335 and 4335) indicating
both unmounted or mounted pump unit.
MODEL NUMBER CHART
UNMOUNTED PUMP
PACKED
N335 N4335
R335 R4335
P335 P4335
This manual deals only with Series 335 and 4335 HeavyDuty Pumps. Refer to Figures 1 through 20 for general
configuration and nomenclature used in this manual. Pump
specifications and recommendations are listed in Catalog
Section 143, for series 335 and 4335 Heavy-Duty Pumps.
MECH.
SEAL
Units are designated by the unmounted pump model numbers
followed by a letter indicating drive
style.
P =Commerical Speed Reducers
UNITS
DANGER !
Before opening any Viking pump liquid chamber (pumping chamber, reservoir, relief valve
adjusting cap fitting etc.) be sure:
1. That any pressure in chamber has been
completely vented through the suction
or discharge lines or other appropriate
openings or connections.
2. That the driving means (motor, turbine,
engine, etc.) has been “locked out” or made
non- operational so that it cannot be started
while work is being done on the pump.
3. That you know what liquid the pump
has been handling and the precautions
necessary to safely handle the liquid.
Obtain a material safety data sheet (msds)
for the liquid to be sure these precautions
are understood.
Failure to follow the above listed precautionary measures may result in serious injury or
death.
VIKING PUMP, INC. • A Unit of IDEX Corporation • Cedar Falls, IA 50613 USA
Page 2
SPECIAL INFORMATION
ROTATION: Viking pumps operate equally well in a clockwise
or counterclockwise rotation. Shaft rotation determines which
port is suction and which is discharge. The suction port
location is where pumping elements (gear teeth) come out
of mesh.
CIRCULATION LINES: are standard equipment (N & R size
only) and must be properly connected. Packed pumps have
a line connected from the packing chamber to the discharge
port. Mechanical seal pumps have a line connected from
the seal chamber to the suction port. If the pump rotation is
reversed be sure the circulation lines are connected to the
suction or discharge port as noted above to avoid excessive
leakage or damage to pump. If the pump is handling heated
product be sure the circulation line is insulated to assure
continued flow.
The jacketed head (R & P only, optional on N size) and
rotor bearing sleeve provide large chambers at both ends
of the pumping chamber for temperature control of product
in the pump. These features do not alter basic steps in the
disassembly and assembly of your pump.
PRESSURE RELIEF VALVES:
1. Viking pumps are positive placement pumps and must
be provided with some sort of pressure protection. This
may be a relief valve mounted directly on the pump, an
inline pressure relief valve, a torque limiting device or a
rupture disk.
2. A non-jacketed relief valve is standard on these pumps.
Options include plain and jacketed relief valves. N size
pumps with a jacketed head with a relief valve is not
available . R size pumps are standard with a jacketed
head but also have both plain and jacketed relief valve
available as options. P size pumps are standard with a
jacketed head and non-jacketed relief valve.
3. If the pump rotation is to be reversed during operation,
pressure protection must be provided on both sides of
pump.
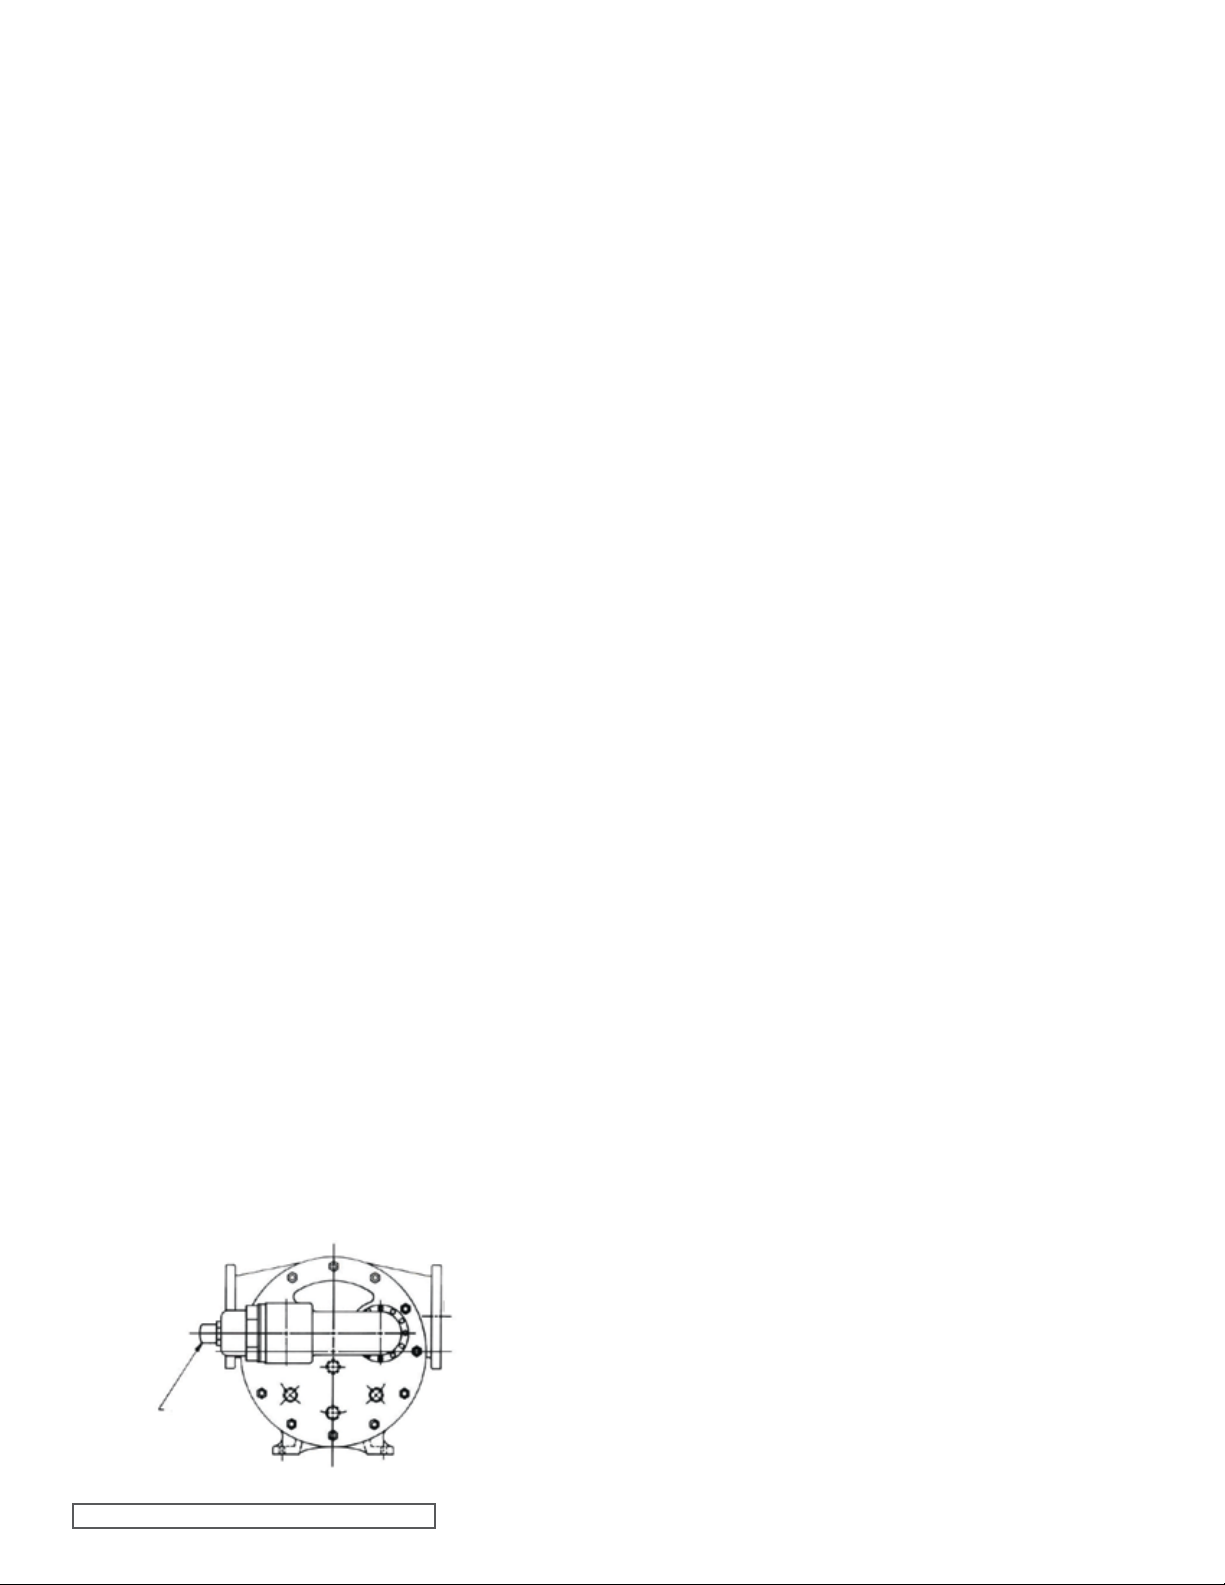
4. The relief valve adjusting screw cap must always point
towards suction side of pump. If pump rotation is
reversed, remove the pressure relief valve and turn end
for end. Refer to Figure 2.
5. Pressure relief valves cannot be used to control the pump
flow or regulate the discharge pressure.
For additional information on pressure relief valves, refer to
Technical Service Manual TSM000 and Engineering Service
Bulletin ESB-31.
INLET
OR
SUCTION
OUTLET
OR
DISCHARGE
SPECIAL MECHANICAL SEALS: can be installed in a
modified stuffing box.
Extra care must be taken in the repair of pumps with
mechanical seals. Read and follow all special information
supplied with the pump.
MAINTENANCE
The Series 335 and 4335 pumps are designed for long
trouble free life under a wide variety of application conditions
with a minimum of maintenance. The points listed below will
help provide long service life.
LUBRICATION: External lubrication must be applied slowly
with a handgun to all lubrication fittings every 500 hours of
operation with multi-purpose grease, NLGI # 2. Do not overgrease. Applications involving very high or low temperatures
will require other types of lubrication. Refer to Engineering
Service Bulleting ESB-515. Consult factory with specific
lubrication questions.
PACKING ADJUSTMENT: New packed pumps require an
initial packing adjustment to control leakage as the packing
“runs in”. Make initial adjustments carefully and do not
over-tighten the packing gland. After the initial adjustment,
inspection will reveal the need for packing gland adjustment
or packing replacement. Refer to instructions under
DISASSEMBLY, page 4, and ASSEMBLY, page 6, regarding
repacking the pump.
CLEANING PUMP: Keep the pump as clean as possible.
This will facilitate inspection; adjustment and repair work and
help prevent overlooking a dirt covered grease fitting.
STORAGE: If the pump is to be stored, or not used for six
months or more, the pump must be drained and a light coat
of non-detergent SAE 30 weight oil must be applied to all
internal pump parts. Lubricate fittings and apply grease to
the pump shaft extension. Viking suggests rotating the pump
shaft by hand one complete revolution every 30 days to
circulate the oil.
SUGGESTED REPAIR TOOLS: The following tools must
be available to properly repair Series 335 and 4335 pumps.
These tools are in addition to standard mechanics’ tools such
as open end wrenches, pliers, screwdrivers etc. Most of the
listed items can be obtained from an industrial supply house.
1. Soft Headed Hammer
2. Allen Wrenches (for some mechanical seals and set
collars)
3. Packing hooks, flexible (packed pumps)
Large for 0.375 inch and up cross section packing
4. Bearing locknut spanner wrench
(Source: #471 J.H. Williams & Co. or equal)
5. Spanner wrench (Supplied with pump)
Viking Part Number 3-810-009-631
RELIEF VALVE
ADJUSTING
SCREW CAP
FIGURE 2
SECTION TSM 143 ISSUE E PAGE 2 OF 15
6. Brass Bar
7. Arbor Press
Page 3
SHAFT
ROLLER
BEARINGS
PACKING
GLAND
ROTOR BEARING
SLEEVE BUSHING
ROTOR BEARING
SLEEVE GASKET
CASING
HEAD GASKET
HEAD
IDLER PIN
END CAP
THRUST
BEARING
HOUSING
BEARING
HOUSING
STAND
PACKING
ROTOR
BEARING
SLEEVE
ROTOR
IDLER
FIGURE 3
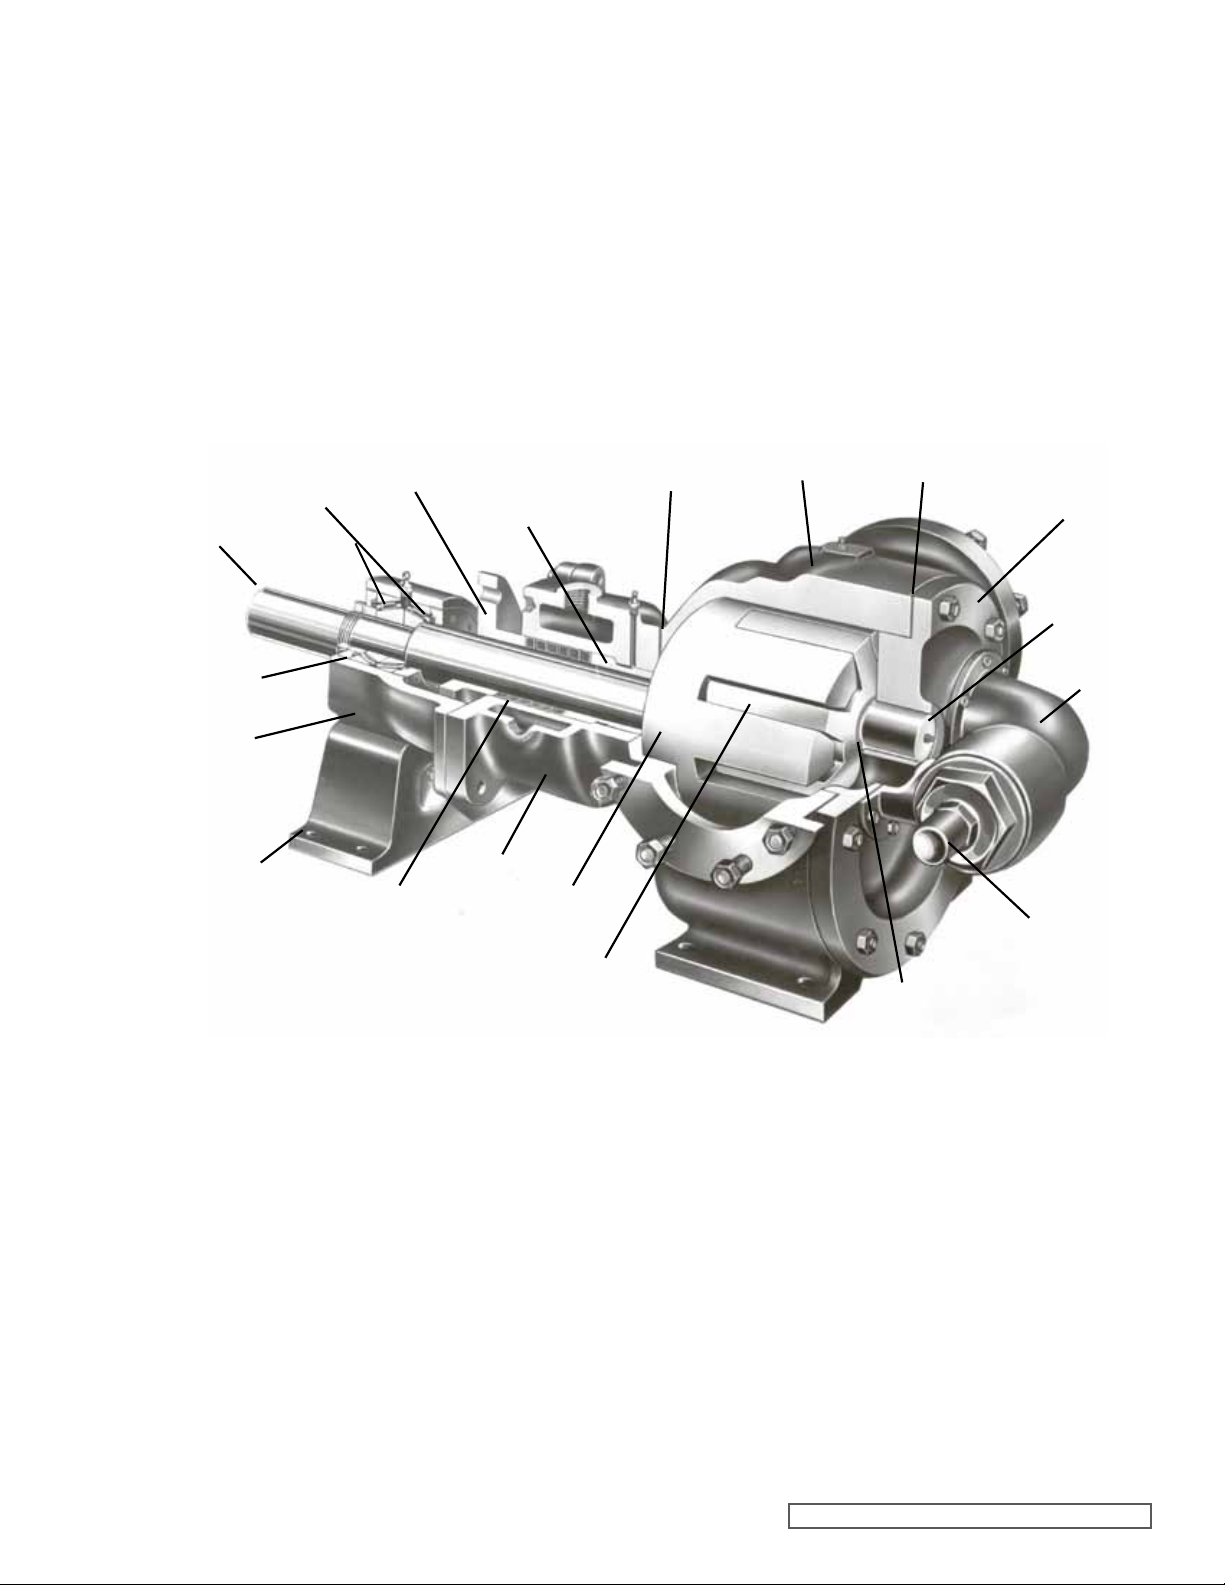
CUTAWAY OF PACKED PUMP MODEL N335
RELIEF
VALV E
RELIEF VALVE
ADJUSTING
SCREW CAP
IDLER
BUSHING
SECTION TSM 143 ISSUE E PAGE 3 OF 15
Page 4
PACKED PUMPS
Model N, R, and P335
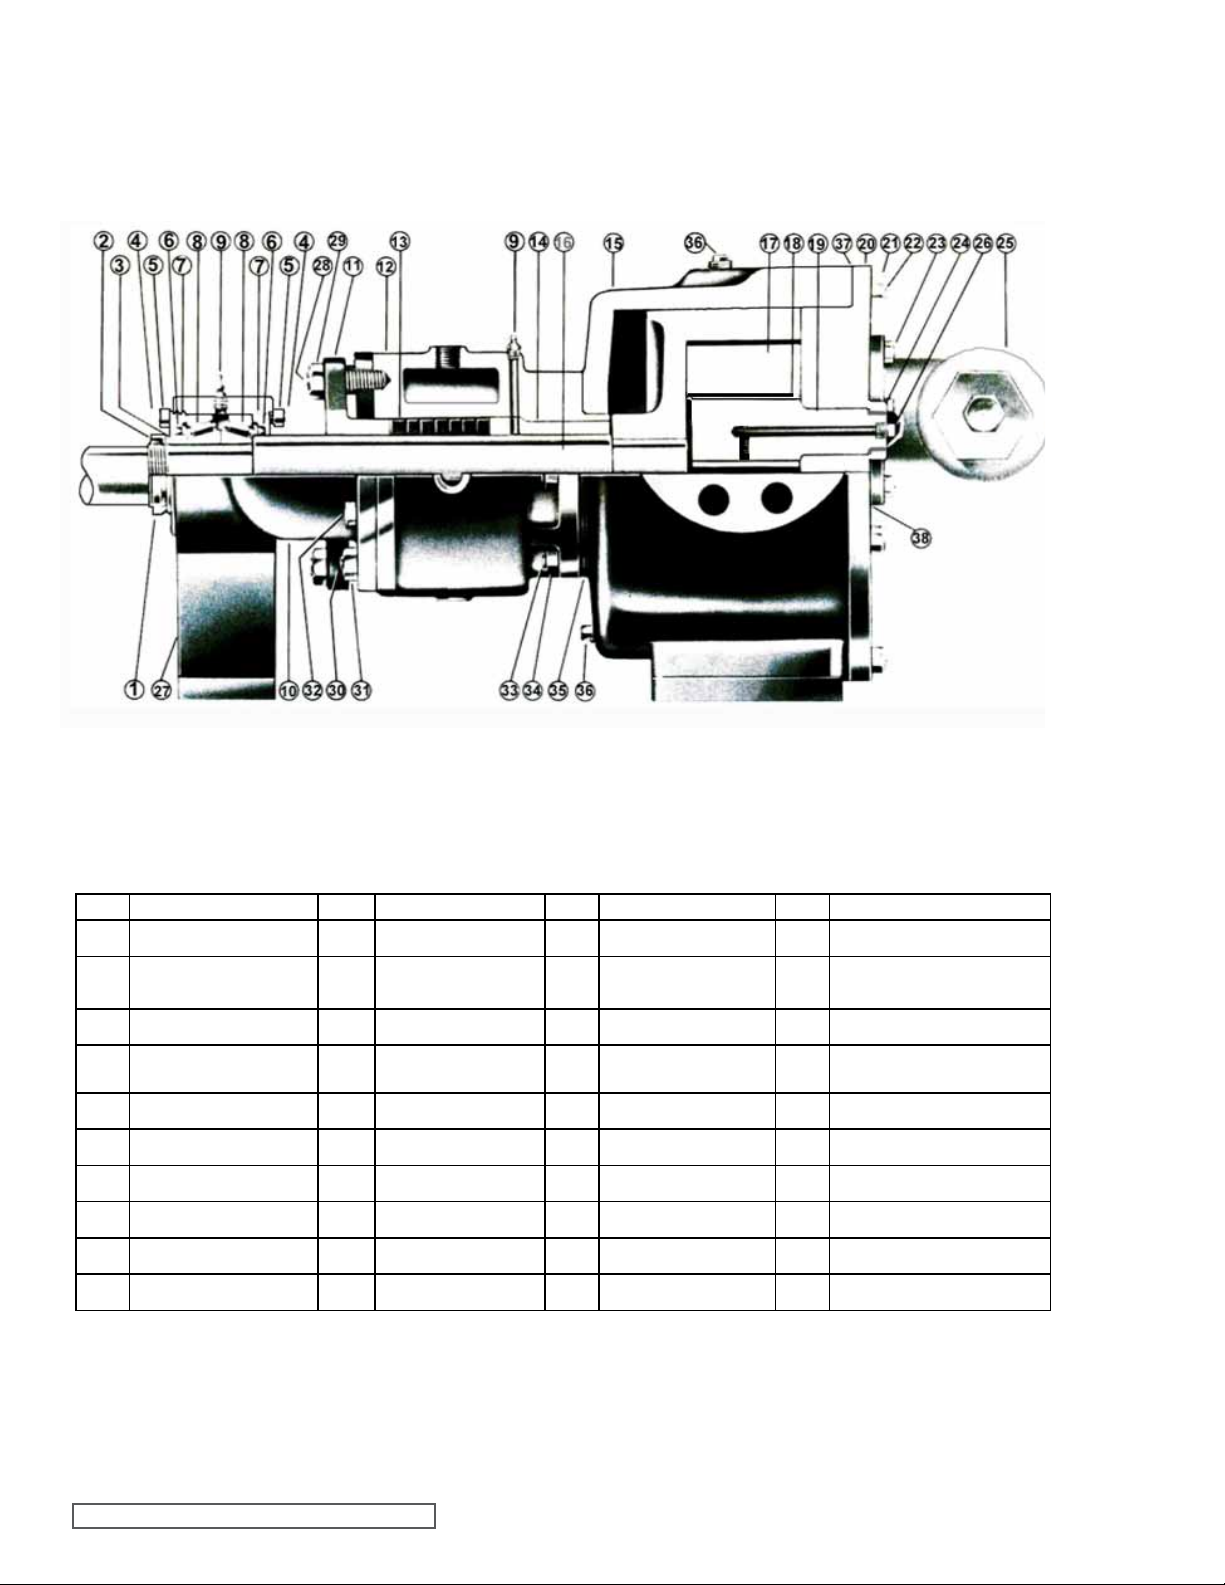
FIGURE 4 DETAILS FOR SECTIONAL VIEW - MODELS N, R AND P335
ITEM NAME OF PART ITEM NAME OF PART ITEM NAME OF PART ITEM NAME OF PART
1 Locknut 11 Packing Gland 21 Nut For Head 31 Bearing Housing Nut
2 Lockwasher 12
3 Bearing Spacer Collar 13 Packing 23 Capscrew For Valve 33
Capscrew for Adjusting
4
Locknut
5 End Cap Lock 15 Casing 25 Internal Relief Valve 35 Rotor Bearing Sleeve Gasket
6 Lip Seal 16 Rotor and Shaft 26 Pipe Plug 36 Pipe Plug
7 End Cap 17 Idler and Bushing 27 Bearing Housing Stand 37 Head Gasket
8 Roller Bearing 18 Idler Bushing 28 Packing Gland Stud 38 Relief Valve Gasket
9 Grease Fitting 19 Idler Pin 29 Packing Gland Nut * Suck Back line Not Illus.
10 Thrust Bearing Housing 20 Head and Idler Pin 30 Bearing Housing Stud
Rotor Bearing Sleeve
& Bushing
Bushing, Rotor
14
Bearing Sleeve
22 Stud For Head 32 Bearing Housing Capscrew
Stud For Rotor Bearing
Sleeve
24 Idler Pin Nut (Not N) 34 Nut For Rotor Bearing Sleeve
SECTION TSM 143 ISSUE E PAGE 4 OF 15
Page 5
DANGER !
Before opening any Viking pump liquid chamber (pumping chamber, reservoir, relief valve
adjusting cap fitting etc.) Be sure:
1. That any pressure in the chamber has been
completely vented through the suction
or discharge lines or other appropriate
openings or connections.
2. That the driving means (motor, turbine,
engine, etc.) has been “locked out” or made
non- operational so that it cannot be started
while work is being done on the pump.
3. That you know what liquid the pump
has been handling and the precautions
necessary to safely handle the liquid.
Obtain a material safety data sheet (MSDS)
for the liquid to be sure these precautions
are understood.
Failure to follow above listed precautionary measures may result in serious injury or
death.
DISASSEMBLY
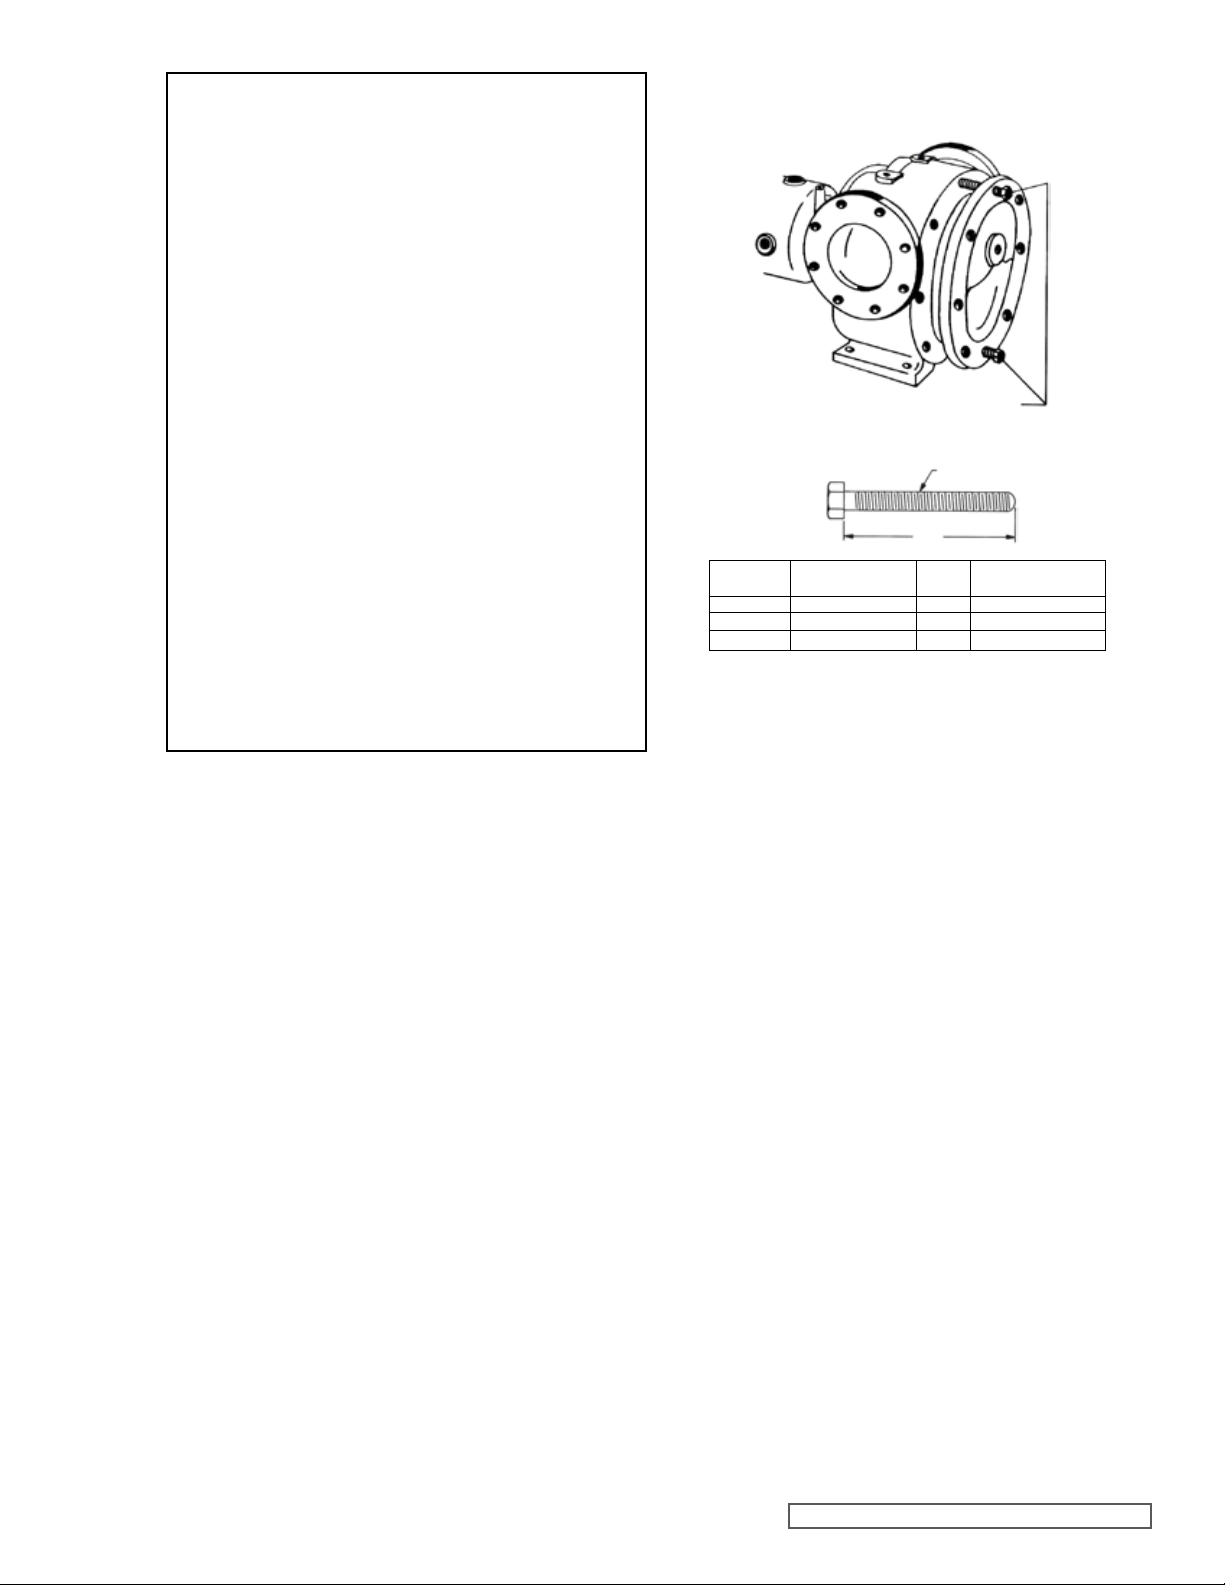
1. Mark the head and casing before disassembly to ensure
proper reassembly. The idler pin, which is offset in pump
head, must be positioned towards and equal distance
between the port connections to allow for proper flow of
liquid through the pump.(Refer to figure 5)
It is not necessary to remove the relief valve to take the
head off the pump; however, removing the relief valve
will lessen the total weight of the part. Do not use chain
or cable around the relief value body to support the
head during removal. For PRESSURE RELIEF VALVE
INSTRUCTIONS, refer to page 14.
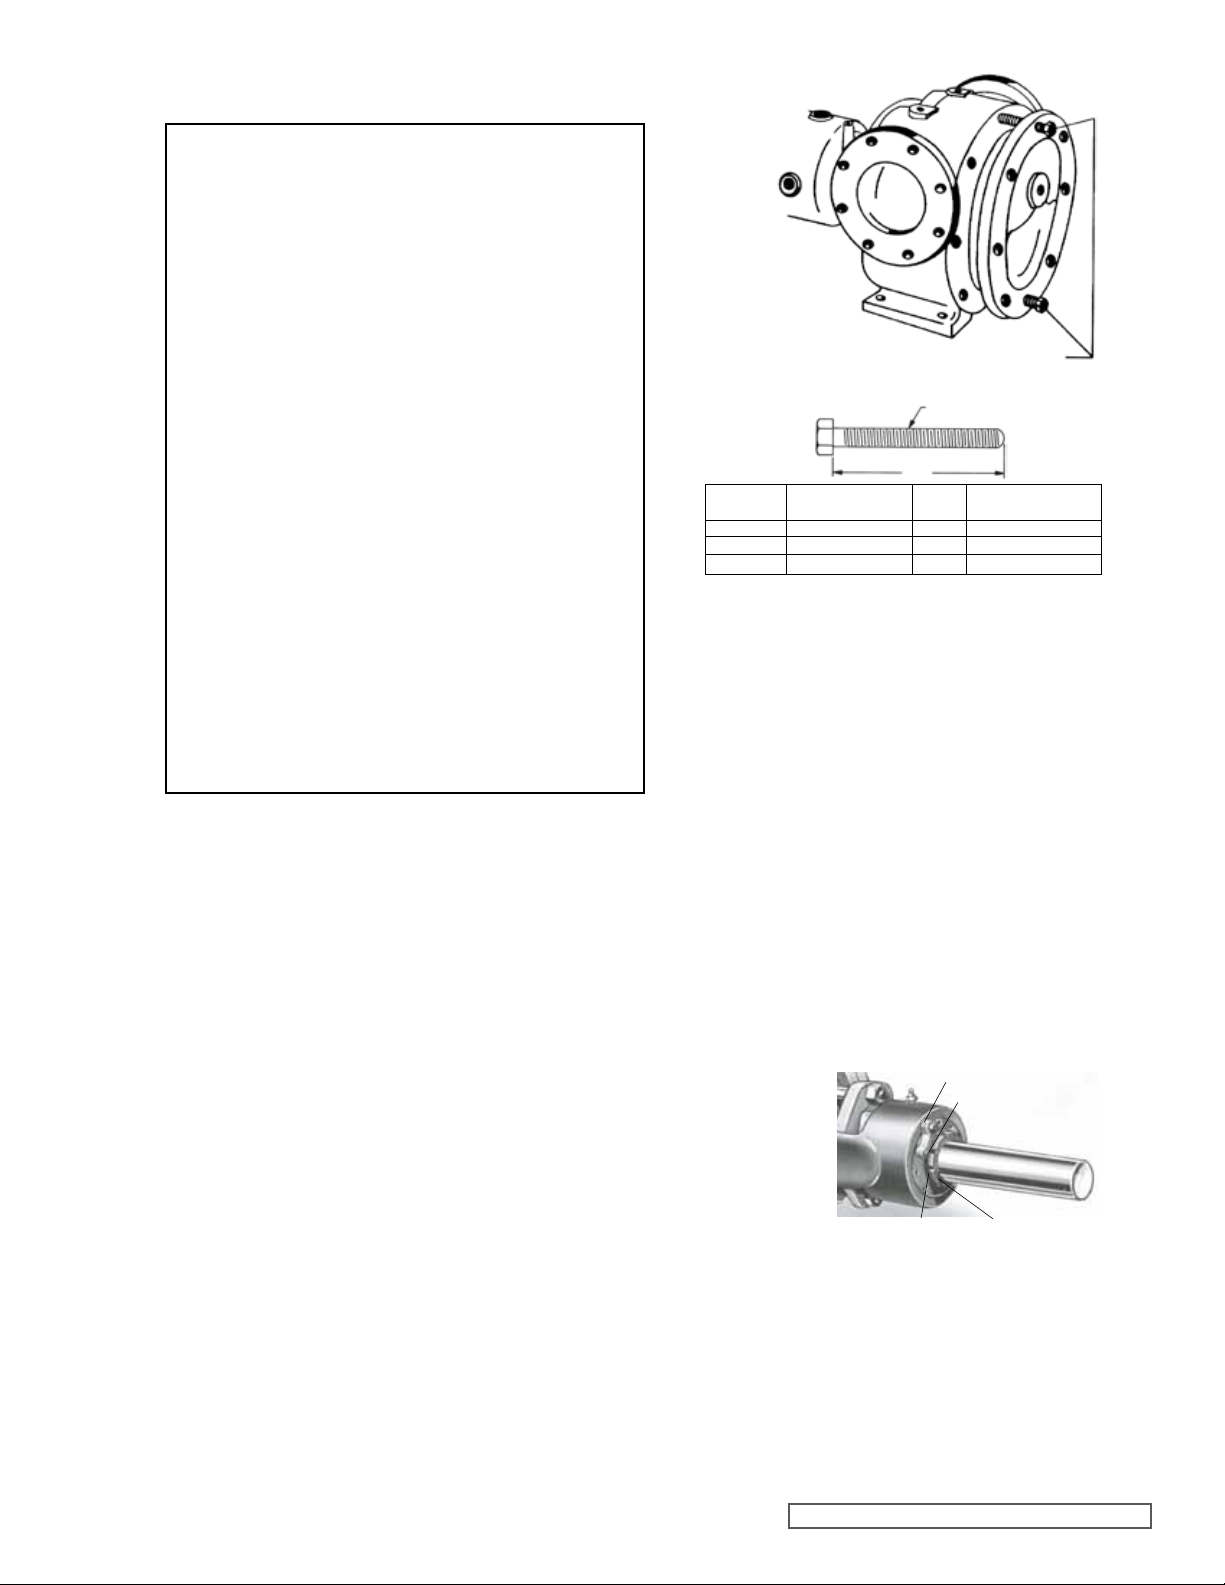
Remove all nuts from the head. Jackscrews should be
used to back the head away from the casing as shown
in Figure 5. For proper size and length of jackscrews for
pump size refer to the table in Figure 6. The use of a hoist
to support head will facilitate its removal.
Back the head away from casing. Do not allow the idler
to fall from the idler pin. To prevent this, tilt the top of the
head back when removing. Remove the head from pump.
If a hoist is not available, cribbing or blocking can be used
to support head. This will eliminate having to lift the head
into position when reassembling the pump.
2. Remove the head gasket, idler and bushing assembly.
3. Remove the pipe plug from the drain hole in the casing,
this breaks the vacuum behind rotor.
JACKSCREWS
FIGURE 5
THREAD SIZE
A
PUMP
SIZE
N 2 4.00 0.50” - 13 NC
R 2 4.50 0.63” - 11 NC
P 3 5.00 0.50” - 13 NC
4. Remove the packing gland nuts and slide the gland out
of the rotor bearing sleeve.
5. Insert a length of hard wood or brass bar through the
port opening between the rotor teeth to keep the shaft
from turning.
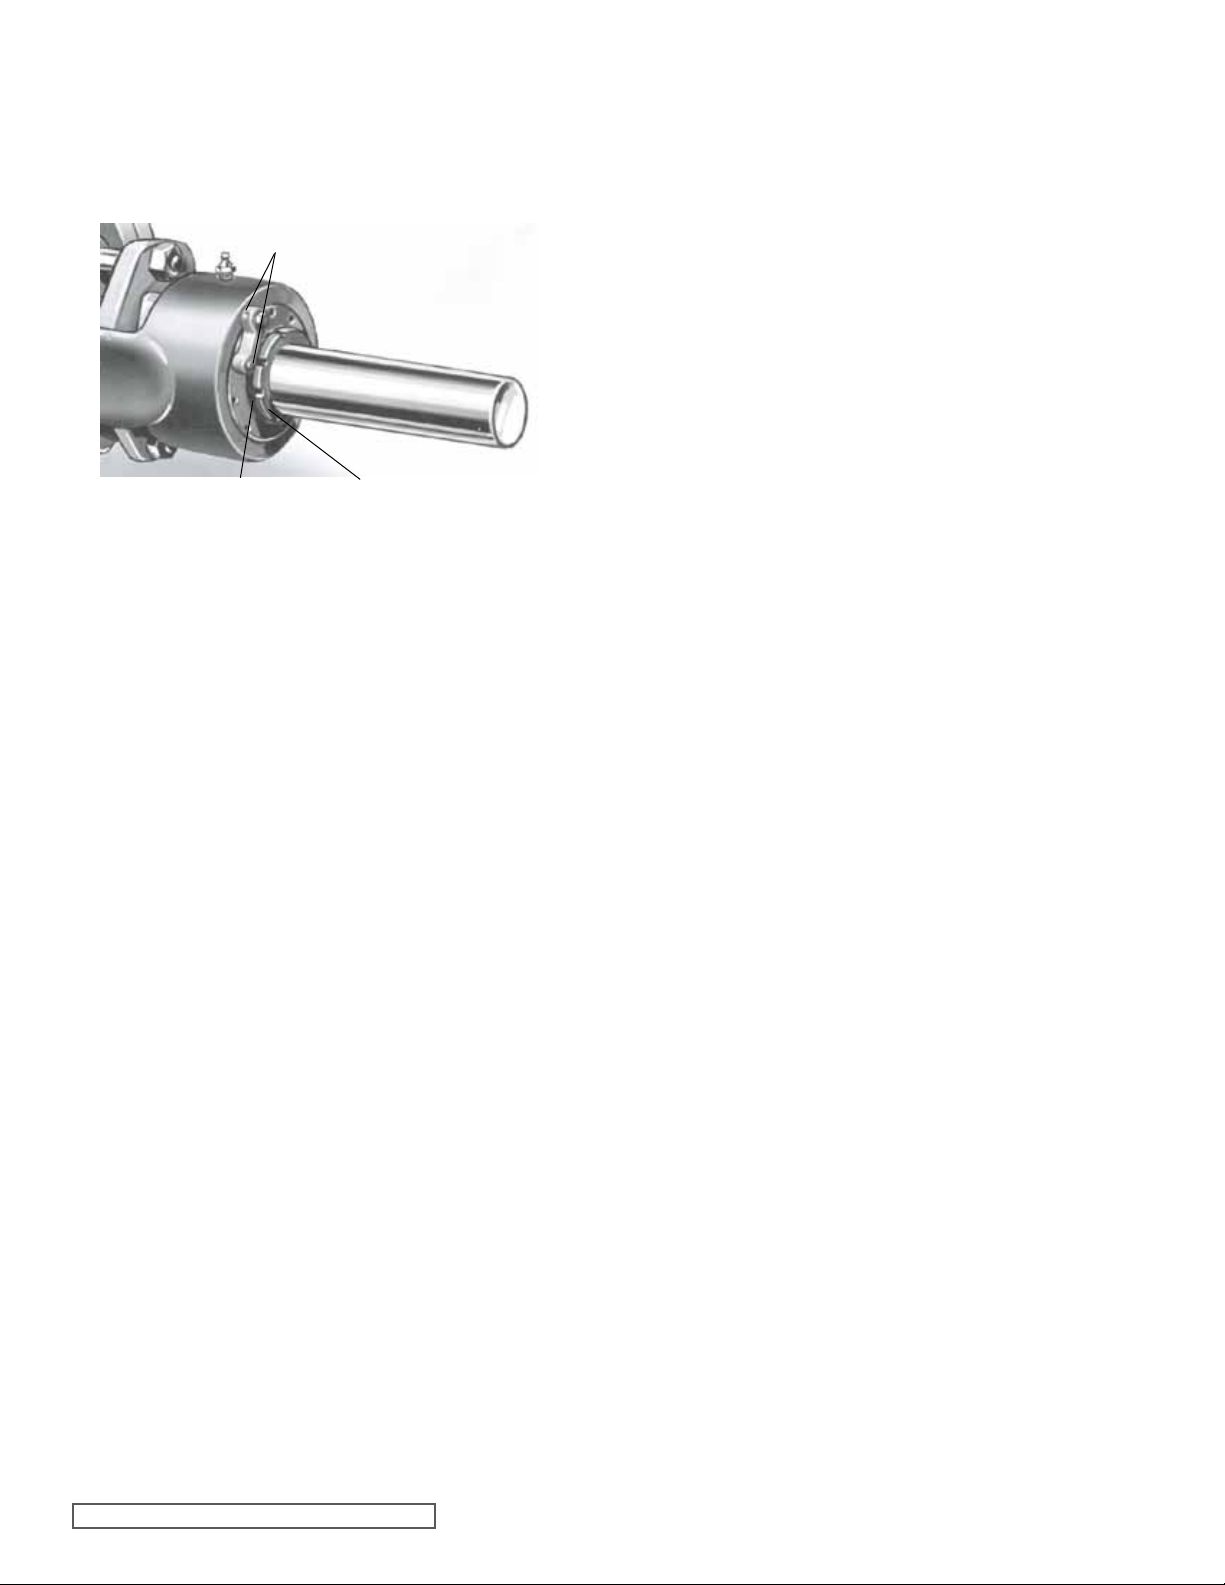
6. Bend the tang on the lock washer up, and with a spanner
wrench remove the locknut and lockwasher from the
shaft. Refer to Figure 7.
7. Remove the length of hardwood or brass bar from the
port opening.
8. Cushion the end of the shaft with a hardwood block or
piece of brass and drive the rotor out of casing, being
careful to avoid damaging the rotor bearing sleeve
bushing. Support the weight of rotor with a hoist. A cable
sling can be used around the shaft, or around rotor
teeth, to carry the weight of the part.
9. Remove the end cap lockscrews, disengage the end cap
locks and with a spanner wrench remove the end caps.
Remove the roller bearings.
10. Remove the nuts and capscrews and take off the thrust
bearing housing. Remove the packing from the rotor
bearing sleeve. NOTE: Model P335 has a lantern ring.
11. Check the rotor bearing sleeve bushing while the rotor
bearing sleeve is mounted on the casing. If worn, the
bushing must be replaced.
Disconnect the circulation line and remove the rotor
bearing sleeve from casing. A press must be used to
remove the old bushing. If the bushing has a shoulder
on the stuffing box end, it must be pressed out through
NO. SCREWS
USED
FIGURE 6
MINIMUM JACKSCREW LENGTH
SECTION TSM 143 ISSUE E PAGE 5 OF 15
A
THREAD SIZE
(INCH)
Page 6
the packing end of the rotor bearing sleeve. If the
bushing is carbon graphite, refer to INSTALLATION OF
CARBON GRAPHITE BUSHINGS, page 13.
ADJUSTING NUT LOCK WITH
SELF-LOCKING PIN
LOCKWASHER WITH TANG
LOCKNUT
FIGURE 7
12. Clean all parts thoroughly and examine for wear and
damage. Check the idler bushing and idler pin; replace
if necessary.
If the idler pin is to be replaced, the oil groove must be
installed facing the center of the crescent on the head.
If lipseals need replacement, press into the end cap,
with the lip facing the bearings.
If the idler bushing is to be replaced, a press must be
used to remove the old bushing and install the new one.
The bushing position after being pressed in should be
flush with the face of the idler. For a carbon graphite
idler bushing, refer to INSTALLATION OF CARBON
GRAPHITE BUSHINGS, page 13.
Wash the anti-friction bearings (roller bearings) in clean
solvent. Blow out the bearings with compressed air. Do
not allow the bearings to spin; turn the bearing slowly by
hand. Spinning the bearings will damage the race and
rollers. Make sure the bearings are clean, then lubricate
with non-detergent SAE 30 weight oil and check for
roughness. Roughness can be determined by turning
the outer race by hand. CAUTION: do not intermix the
inner and outer races for the roller bearings. Replace
the bearings if they have roughness.
Examine the casing for wear. Check the condition of
the casing at the sealing area (surface between suction
and discharge port). If the surface is in good condition,
the casing need not be replaced.
When making major repairs, such as replacement of a
rotor, it is usually considered advisable to install a new
head and idler. When making minor repairs, where only
an idler bushing and idler pin are required, other new
parts are usually not necessary.
SECTION TSM 143 ISSUE E PAGE 6 OF 15
ASSEMBLY
1. Install the rotor bearing sleeve and gasket on the casing.
Coat both sides of the gasket with thread sealant (pipe
dope) and quickly install the gasket and rotor bearing
sleeve on the casing. Place a support under the
rotor bearing sleeve to prevent the casing and rotor
bearing sleeve from tilting down while the rotor is being
installed.
2. Check the casing to be sure the drain plug has been
removed.
3. Carefully check the shaft, remove any burrs or rough
surfaces to avoid damaging the rotor bearing sleeve
bushing while installing the rotor and shaft into the
casing. Coat the inner diameter of the rotor bearing
sleeve bushing and shaft with a thin coat of nondetergent SAE 30 weight oil.
Support the weight of the rotor with a hoist. A cable sling
can be used around the shaft, or rotor teeth to carry
the weight of the part while being assembled into the
casing.
Place the end of the rotor shaft through the casing,
into the bushing slowly turn rotor from right to left while
pushing into the casing. When the shaft first protrudes
from stuffing box, stop pushing. Check to see if the large
diameter of the shaft has protruded far enough into rotor
bearing sleeve to permit installing packing rings.
Use packing suitable for the liquid being pumped.
Lubricate packing rings with oil, grease or graphite to aid
assembly. Packing ring joints should be staggered from
one side of shaft to the other. A length of pipe will help
set each packing ring.
4. Place the packing gland and inner end cap (position
spanner wrench holes on side next to packing gland)
with lip seal (lip facing away from packing gland) over
the end of the shaft.
5. Push the rotor as far into the casing as it will go.
6. Prior to installing the head, coat the casing face with
thread sealant (pipe dope) and place a new .015” head
gasket on the mounting studs. Coat the dry side of
gasket with thread sealant (pipe dope) Place the idler
assembly on the idler pin and prepare to mount the head
and idler assembly. (CAUTION! do not drop the idler on
the foot)
The pump head and casing were marked before
disassembly to ensure proper reassembly. If not, be
sure the idler pin, which is offset in the pump head, is
positioned toward, and equal distance between, the port
connections to allow for proper flow of liquid through the
pump. Place the head on the pump, slightly tilting the
top of the head back away from casing until the crescent
enters the inside diameter of rotor. Rotate the idler on
idler pin until the idler teeth mesh with the rotor teeth.
Raise the head until the face of the head is parallel with
face of the casing and work into position. Care must be
taken to avoid damaging the head gasket. Fasten to the
head to casing with nuts and tighten evenly.
Page 7
If the relief valve was not removed from head, install
on head with adjusting screw cap pointed toward the
suction port. Refer to Figure 2, page 2. For PRESSURE
RELIEF INSTRUCTIONS, refer to page 14.
7. Push the rotor back against the head.
8. Install the drain plug in the casing.
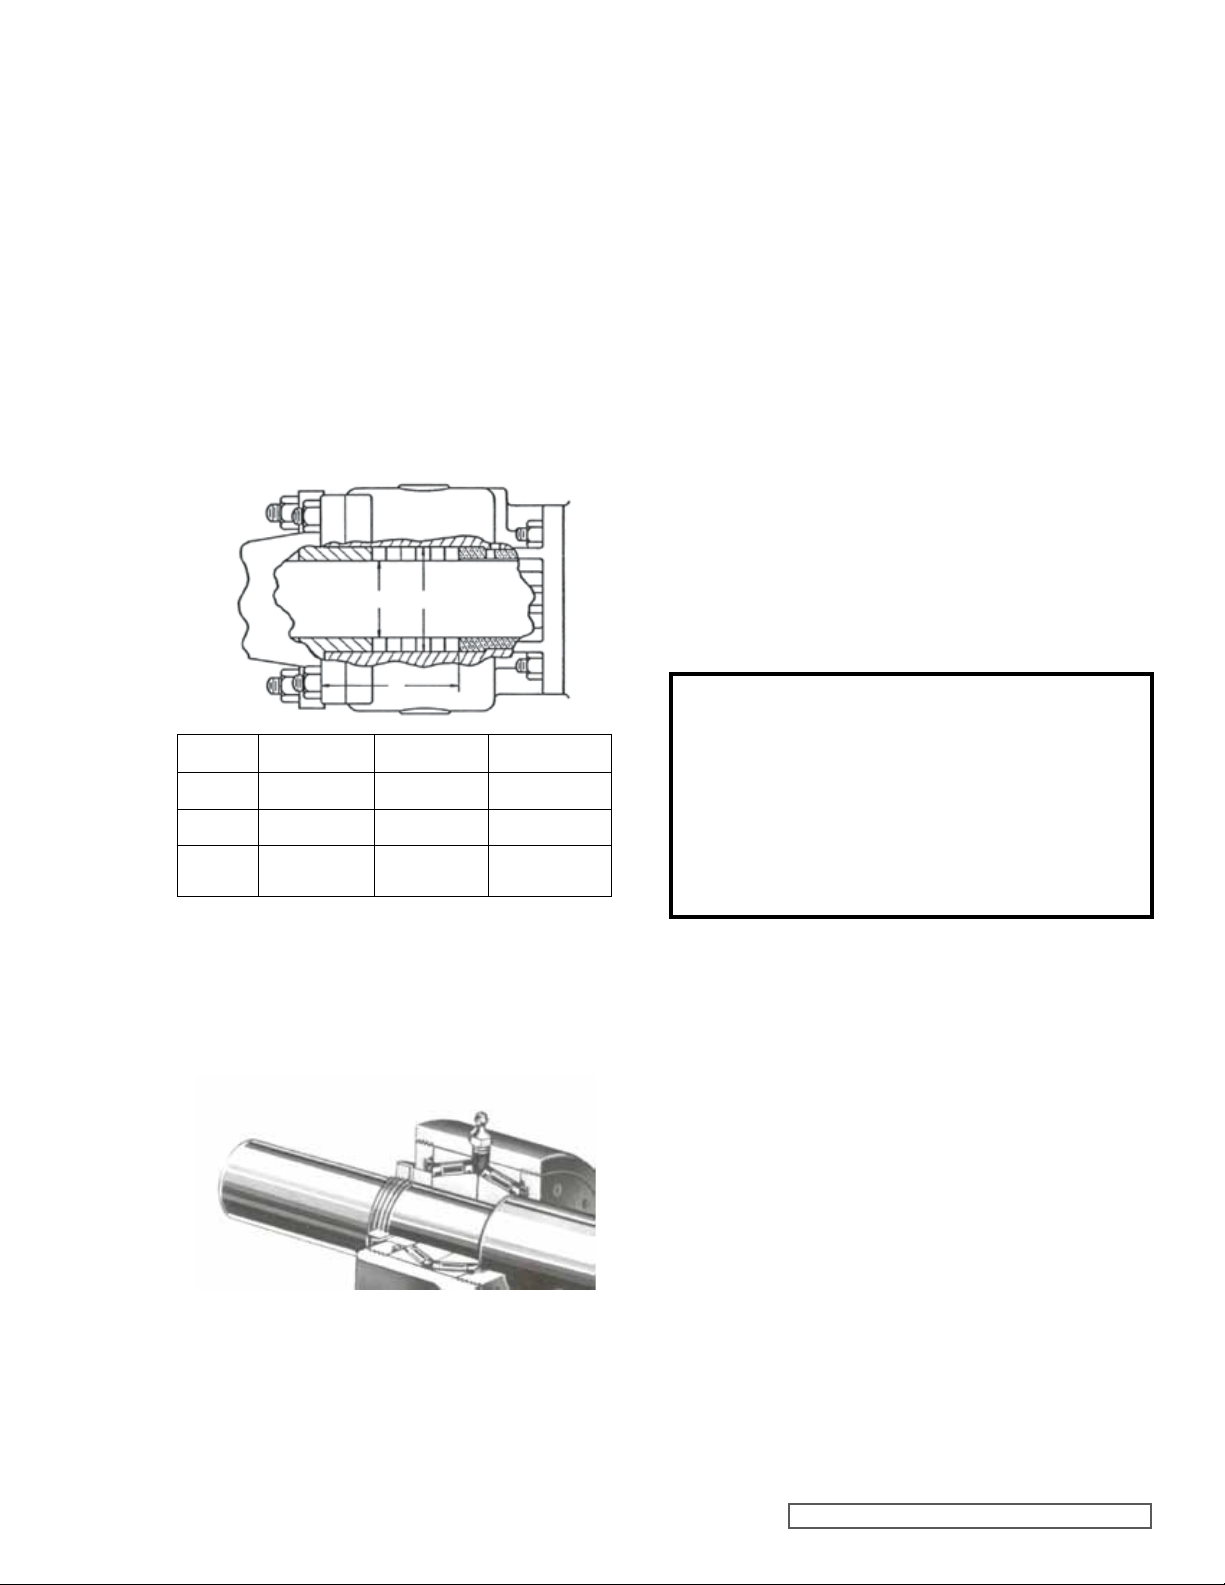
9. Pack the pump with new packing. Refer to Figure 8.
Models N and R335 have 6 rings of packing. Model
P335 has 8 rings of packing and a lantern ring. The
lantern ring should be installed after the fourth ring of
packing has been assembled into the packing box.
10. Install the thrust bearing housing on the end of rotor
bearing sleeve and tighten the nuts and capscrews
securely. It is not necessary to use a gasket between
these parts.
C
B
14. Insert a length of hardwood or brass bar through the port
opening between the rotor teeth to keep the rotor from
turning.
15. Install the lockwasher, placing the tang in the keyway on
the shaft. Tighten the locknut to 170-190 ft – lbs. torque.
Bend one tang of the lockwasher into a slot of locknut.
If tang does not line up with a slot tighten locknut until
it does. Failure to tighten the locknut or engage the
lockwasher tang could result in early bearing failure and
cause damage to rest of the pump.
16. Remove the length of hardwood or brass bar from the
port opening.
17. Install the nuts on the packing gland studs and tighten.
Do not over tighten,as it may cause binding on rotor
shaft.
18. Reinstall the circulation tubing to the casing and rotor
bearing sleeve.
19. Lubricate all grease fittings with multi-purpose grease,
NLGI #2.
20. Adjust the pump end clearance. Refer to THRUST
BEARING ADJUSTMENT, page 13.
A
PUMP
MODEL
N335 4.63 4.69 3.44
R335 5.63 4.69
P335 6.38 5.75 4.50
A (INCH) B (INCH) C (INCH)
3.44
FIGURE 8
STUFFING BOX DIMENSIONS
11. Insert both tapered roller bearings in the thrust bearing
housing, large end of inner races together. It is possible
to install bearings incorrectly, for proper assembly refer
to Figure 9.
DANGER !
Before starting the pump, be sure all drive
equipment guards are in place.
Failure to properly mount the guards may result in serious injury or death.
FIGURE 9
12. Install the bearing spacer collar on the shaft next to the
inner race of the roller bearing.
13. Turn the inner end cap into the thrust bearing housing
just far enough to hold in place.
Install the outer end cap and turn in approximately half
way.
SECTION TSM 143 ISSUE E PAGE 7 OF 15
Page 8
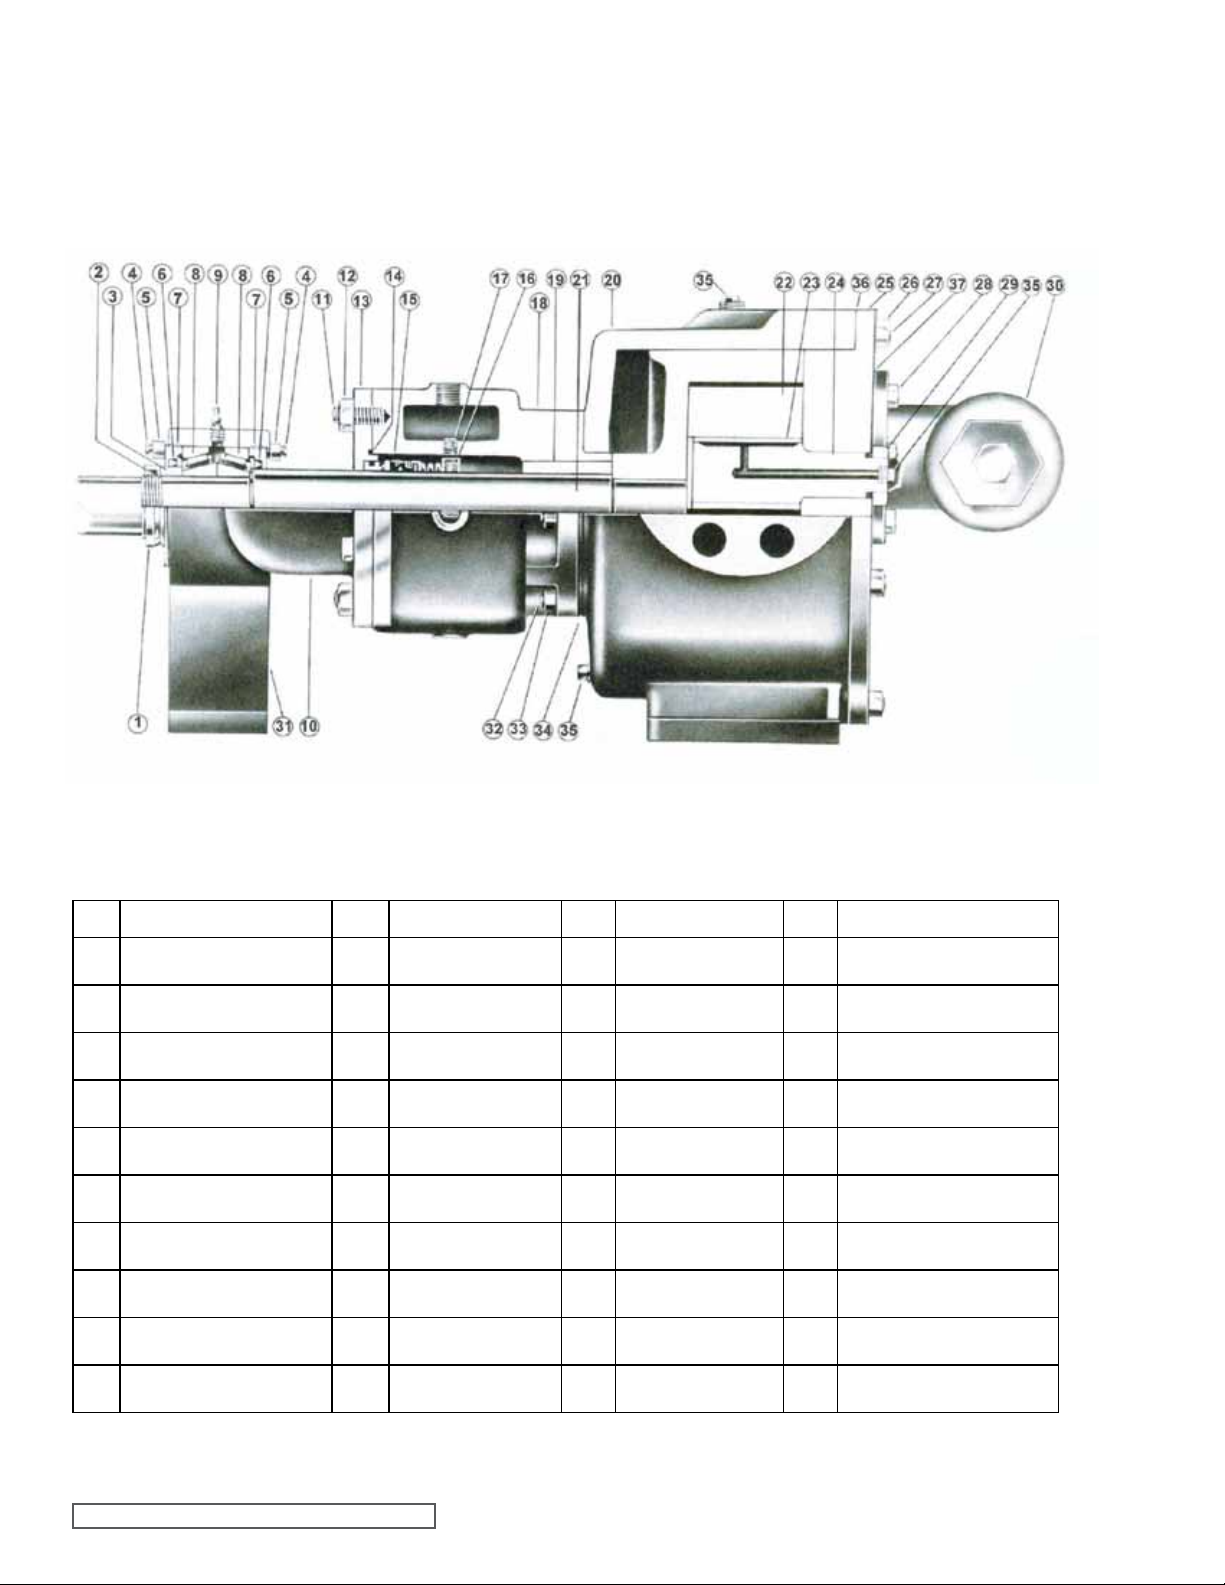
MECHANICAL SEAL PUMPS
Model N, R AND P4335
FIGURE 10 DETAILS FOR SECTIONAL VIEW - MODELS N, R AND P4335
ITEM NAME OF PART ITEM NAME OF PART ITEM NAME OF PART ITEM NAME OF PART
1 Locknut 11 Stud For Seal Plate 21 Rotor and Shaft 31 Bearing Housing Stand
2 Lockwasher 12 Nut For Seal Plate 22 Idler & Bushing 32
3 Bearing Spacer Collar 13 Seal Plate 23 Idler Bushing 33 Nut For Rotor Bearing Sleeve
Lockscrew for Adjusting
4
Locknut
5 End Cap Lock 15
6 Lip Seal 16
7 End Cap 17
8 Roller Bearing 18
9 Grease Fitting 19
10 Thrust Bearing Housing 20 Casing 30 Internal Relief Valve
14 O-Ring Gasket 24 Idler Pin 34 Rotor Bearing Sleeve Gasket
Mechanical Seal
(Complete)
Set Collar with Set
Screws
Pipe Plug ¼ Socket
Head
Rotor Bearing Sleeve
& Bushing
Bushing, Rotor Bearing
Sleeve
25 Head and Idler Pin 35 Pipe Plug
26 Nut For Head 36 Head Gasket
27 Stud For Head 37 Relief Valve Gasket
28 Capscrew For Valve * Flush line Not Illus.
29 Idler Pin Nut (Not N)
Stud For Rotor Bearing
Sleeve
SECTION TSM 143 ISSUE E PAGE 8 OF 15
Page 9
DISASSEMBLY
DANGER!
Before opening any Viking pump liquid chamber (pumping chamber, reservoir, relief valve
adjusting cap fitting etc.) Be sure:
1. That any pressure in the chamber has been
completely vented through the suction
or discharge lines or other appropriate
openings or connections.
2. That the driving means (motor, turbine,
engine, etc.) has been “locked out” or made
non- operational so that it cannot be started
while work is being done on the pump.
3. That you know what liquid the pump
has been handling and the precautions
necessary to safely handle the liquid.
Obtain a material safety data sheet (MSDS)
for the liquid to be sure these precautions
are understood.
Failure to follow the above listed precautionary measures may result in serious injury or
death.
FIGURE 11
JACKSCREWS
THREADSIZE
A
PUMP
SIZE
N 2 4.00 0.50” - 13 NC
R 2 4.50 0.63” - 11 NC
P 3 5.00 0.50” - 13 NC
NO. SCREWS
USED
A
THREAD SIZE
(INCH)
FIGURE 12
MINIMUM JACKSCREW LENGTH
on top of the rotor bearing sleeve, remove the 0.25”
socket head pipe plug. Through the same hole loosen
the 0.313” socket head setscrews which locks the collar
to the shaft. Rotate shaft to be sure all setscrews have
been loosened. Refer to figure 10, page 8, items 16 and
17, for the pipe plug to remove and the setscrews to be
loosened.
1. Mark the head and casing before disassembly to ensure
proper reassembly. The idler pin, which is offset in the
pump head, must be positioned towards and equal
distance between the port connections to allow for
proper flow of liquid through the pump.(Refer to figure
5)
It is not necessary to remove the relief valve to take the
head off the pump; however, removing the relief valve
will lessen total weight of the part. Do not use a chain or
cable around the relief value body to support head during
removal. For PRESSURE RELIEF INSTRUCTIONS,
refer to page 13.
Remove the nuts from the head. Jackscrews should be
used to back the head away from the casing. Refer to
Figure 11 . The proper size and length of jackscrews for
the pump size are shown in Figure 12. The use of a hoist
to support the head will facilitate its removal.
Back the head away from casing. Do not allow the idler
to fall from the idler pin. To prevent this, tilt the top of
head back when removing. Remove head from the
pump. If a hoist is not available, cribbing or blocking can
be used to support the head. This will eliminate having to
lift the head into position when reassembling the pump.
2. Remove the head gasket, idler and bushing assembly.
3. To remove the rotor, loosen the set collar behind the
mechanical seal. Through the one inch jacket connection
4. Remove the casing drain plug to break the vacuum
between back of the rotor and the casing. Remove
any deposits of material from the exposed portion of
the shaft between the seal plate and the thrust bearing
assembly.
5. Insert a length of hardwood or brass through the port
opening between the rotor teeth to keep the shaft from
turning.
6. Bend the tang on the lockwasher up and with a spanner
wrench, remove the locknut and lockwasher from the
shaft. Refer to Figure 13.
ADJUSTING NUT LOCK
SELF-LOCKING PIN
LOCKWASHER WITH TANG
LOCKNUT
FIGURE 13
7. Remove the length of hardwood or brass bar from the
port opening.
8. Cushion the end of the shaft with a hardwood block or
piece of brass and drive the rotor out of the casing being
careful to avoid damaging rotor bearing sleeve bushing.
Support the weight of rotor with a hoist. A cable sling can
be used around the shaft, or around the rotor teeth to
carry the weight of the part.
9. Loosen the end cap lockscrews, disengage the end cap
SECTION TSM 143 ISSUE E PAGE 9 OF 15
Page 10
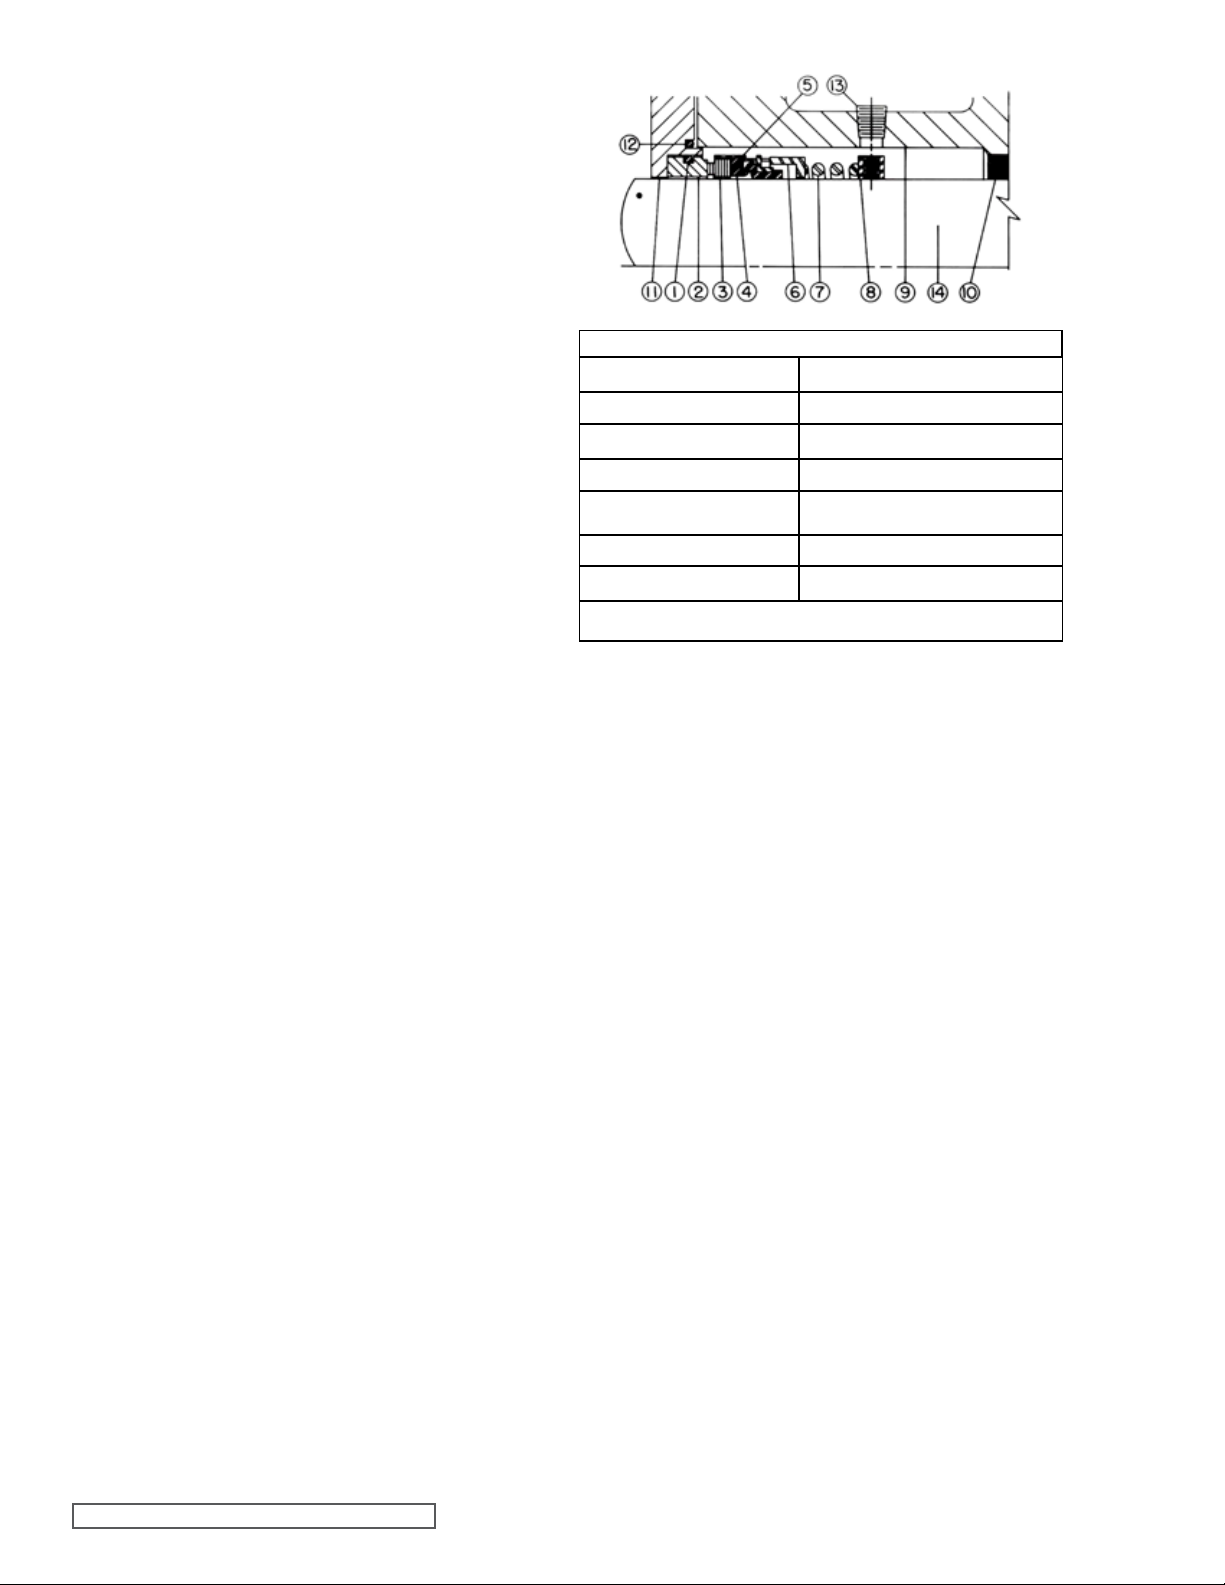
locks and with a spanner wrench, remove the end caps.
Examine the lipseal and replace if worn.
Remove the roller bearings.
10. Remove the nuts and capscrews and take off the thrust
bearing housing.
11. Remove the nuts holding the seal plate and remove seal
plate. The stationary seal seat can be removed from the
seal plate and the rotating portion of the seal from the
rotor bearing sleeve, remove the spring and set collar
from the bottom of the seal chamber.
12. Check rotor the bearing sleeve bushing while the rotor
bearing sleeve is mounted on the casing. If worn, the
bushing must be replaced.
Disconnect the flush line and remove the rotor bearing
sleeve from the casing.
A press must be used to remove the old bushing. If
the bushing has a shoulder on the stuffing box end,
it must be pressed out from the mechanical seal end
of the rotor bearing sleeve. Carbon graphite bushings
are standard for Model 4335 pumps. To replace carbon
graphite bushings, refer to INSTALLATION CARBON
GRAPHITE BUSHINGS, page 12.
LIST OF PARTS
1. O-Ring Seat Gasket
2. Stationary Seat 9. Rotor Bearing Sleeve
3. Rotating Face (Washer) 10. Rotor Bearing Sleeve Bushing
4. Bellows 11. Seal Holder Plate
5. Metal Parts
(retainer, drive band)
6. Spring Adapter 13. Pipe Plug
7. Spring 14. Shaft
NOTE: Items one through seven comprise the complete mechanical seal
8. Set Collar with set screws
12. O-Ring Gasket for seal holder
plate
13. Clean all parts thoroughly and examine for wear and
damage. If lipseal replacement is needed, press in the
end cap with the lip facing the end of the shaft. Check
the idler bushing and idler pin, replace if necessary.
If the idler pin is to be replaced, the oil groove on the
pin must be installed facing the center of the crescent
on the head.
If the idler bushing is to be replaced, a press must
be used to remove the old bushing and install new.
The bushing position after being pressed in should
be flush with teh face of the idler. For carbon graphite
idler bushing, refer to INSTALLATION OF CARBON
GRAPHITE BUSHINGS, page 12.
14. Wash the bearing in clean solvent. Blow out bearings
with compressed air. Do not allow the bearings to spin;
turn the bearing slowly by hand. Spinning the bearings
will damage the race and rollers. Make sure the
bearings are clean, then lubricate with non-detergent
SAE 30 weight oil and check for roughness. Roughness
can be determined by turning the outer race by hand.
CAUTION: do not intermix the inner and outer races for
the roller bearings.
15. Examine the casing for wear. Check the condition of
the casing at the seal area (surface between suction
and discharge ports). If the surface is in good condition,
the casing need not be replaced. When making major
repairs, such as replacement of a rotor, it is usually
considered advisable to install a new head and idler.
When making minor repairs, when only an idler bushing
and idler pin are required, other new parts are usually
not necessary.
16. Inspect the mechanical seal for wear or damage.
Refer to Figure 14 for mechanical seal list of parts. In
general, if the pump has been operated long enough
to exhibit other worn parts, it is likely the seal will have
FIGURE 14 MECHANICAL SEAL
to be replaced. Replacing individual seal parts is not
recommended, i.e., a used seal washer will not perform
satisfactorily when run against a new stationary seat.
ASSEMBLY
Standard Mechanical Seal (Synthetic Rubber Bellows Type)
Prepare all parts for reassembly ahead of time. Pack roller
bearings with multi-purpose grease, NLGI # 2 and have all
new gaskets on hand.
Be especially careful to keep mechanical seal parts clean.
Minute dirt particles especially on the seal faces, will cause
leakage. Never touch the seal faces with anything except
clean hands or a clean cloth.
Once the rotating portion of mechanical seal is installed on
rotor shaft, it is necessary to assemble parts as quickly as
possible to ensure the seal does not stick to the shaft in the
wrong axial position. The seal should be expected to stick to
the shaft after several minutes setting time.
1. Deburr the threads on the rotor shaft with a fine file and
place a layer of tape over the threads to protect the rotor
bearing sleeve bushing during assembly. Gently radius
leading edge of the largest diameter on the shaft (.03
inch is sufficient to aid in seal installation). Smooth the
radius with a very fine grit emery cloth. Polish the rotor
shaft from leading edge through mechanical seal area
with the emery cloth. Any scratches left on shaft in seal
area will provide leakage paths under mechanical seal.
2. Install the rotor bearing sleeve and gasket on the casing.
Coat both sides of the gasket with thread sealant (pipe
SECTION TSM 143 ISSUE E PAGE 10 OF 15
Page 11
dope) and quickly install the gasket and rotor bearing
on the casing. Place a support under the rotor bearing
sleeve to prevent the casing and rotor bearing sleeve
from tilting down while the rotor is being installed.
3. Check the casing to be sure the drain plug has been
removed.
4. Coat the inner diameter of the rotor bearing sleeve
bushing with a thin coat of non-detergent SAE 30 weight
oil.
Support the weight of the rotor with a hoist. A cable sling
can be used around the shaft, or around the rotor teeth,
to carry the weight of part while being assembled into
the casing.
Place the end of rotor shaft through casing into bushing.
Do not allow any portion of the shaft to strike the
bushing. A carbon graphite bushing can be severely
damaged if struck. Slowly turn the rotor from right to left
while pushing into the casing. Push the rotor as far into
casing as it will go.
5. Prior to installing the head, coat the casing face with
thread sealant (pipe dope) and place a new .015 inch
head gasket on the mounting studs. Coat the dry side of
the gasket with thread sealant (pipe dope) and prepare
to mount the head and idler assembly.
6. The pump head and casing were marked before
disassembly to ensure proper reassembly. If not, be
sure the idler pin, which is off set in the pump head, is
positioned toward and equal distance between the port
connections to allow for an even flow of liquid through
the pump.
Place the head on pump, slightly tilting top of the head
back away from casing until the crescent enters inside
diameter of the rotor. Rotate the idler on idler pin until
the idler teeth mesh with the rotor teeth. Raise the head
until the face of head is parallel with the face of casing
and then work into position. Care must be taken to avoid
damaging the head gasket. Fasten the head to casing
with head nuts and tighten evenly.
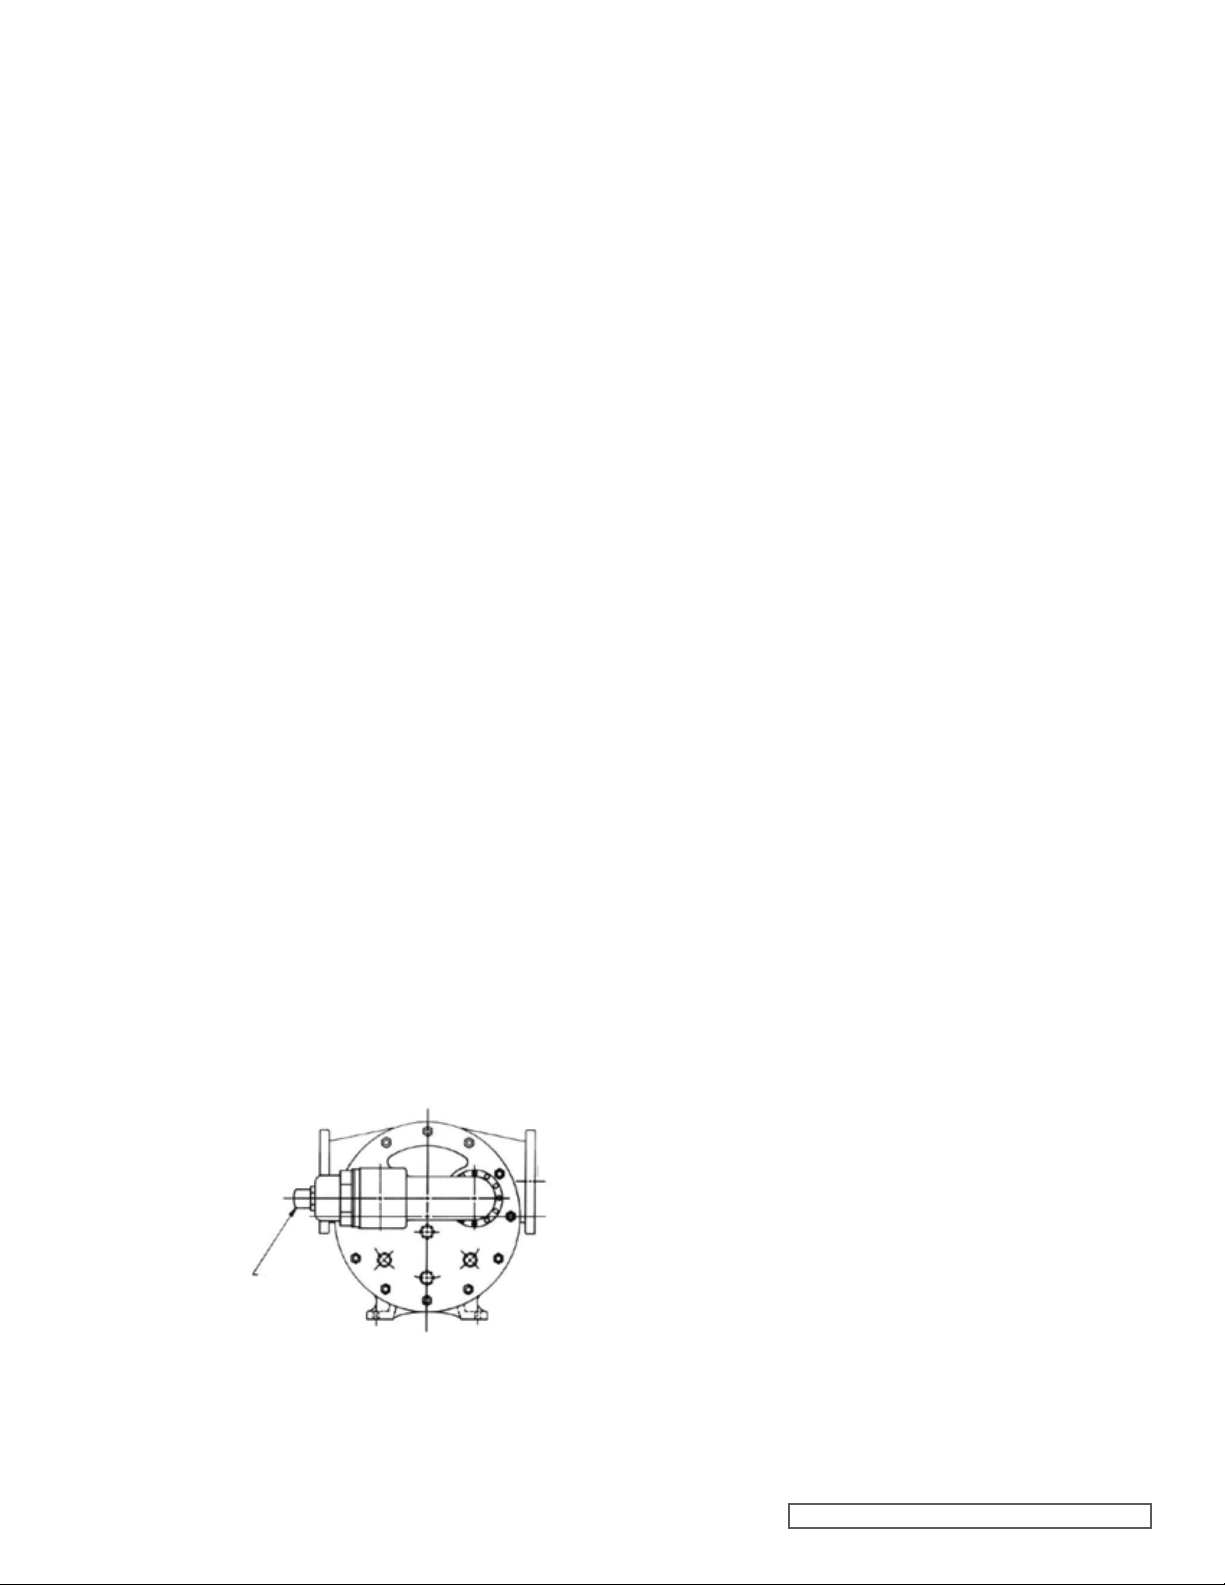
If the relief valve was removed from the head, install on
head with the adjusting screw cap pointed toward suction
port. Refer to figure 15. For PRESSURE RELIEF VALVE
INSTRUCTIONS, refer to page 13.
INLET
OR
SUCTION
RELIEF VALVE
ADJUSTING
SCREW CAP
OUTLET
OR
DISCHARGE
FIGURE 15
7. Push the rotor back against the head.
Install the drain plug in the casing.
9. Wipe the shaft clean in seal area and thoroughly coat
with non-detergent SAE 30 weight oil.
Before installing the parts contained in the mechanical
seal, refer to Figure 14 to become familiar with part
name and location in rotor bearing sleeve.
10. Install the set collar on the shaft in the rotor bearing
sleeve directly under the tapped access hole. The center
line of the collar set screws (5/16” socket head) must
line up with the center line of the access hole. Rotate the
shaft and tighten all setscrews.
Replace the pipe plug in seal access hole.
11. Slide the seal spring on the shaft and into the seal
chamber against the set collar. Place the spring adapter,
with the open side facing the end of shaft against the
spring. Place the tapered installation sleeve on shaft.
NOTE: The tapered installation sleeve is available from
factory, at additional cost, for the N & R size pumps.
12. Apply a generous amount of non-detergent SAE 30
weight oil to the large diameter of the shaft, tapered
installation sleeve and the inner diameter of the
mechanical seal rubber parts.
13. Coat the seal holder chamber and the o-ring seat gasket
with non-detergent SAE 30 weight oil and press in the
seal seat with lapped faced out. Protect the face of the
seal seat with a clean piece of cardboard while pressing
into place.
14. Coat the seal holder plate o-ring gasket with nondetergent SAE 30 weight oil and install over the pilot of
plate.
15. Coat the inside diameter of the rotating face of seal
with non-detergent SAE 30 weight oil and start the tail
of bellows over installation sleeve on shaft. A twisting
motion while pushing will aid in sliding the seal on the
sleeve. Push the seal against seal adapter. Do not touch
the carbon rotating face with anything except clean
hands or a clean cloth.
Check to make sure the adapter is not cocked.
16. Install the seal holder plate over the shaft on mounting
studs until the seal faces touch.
Start the nuts on the mounting studs. Pull the seal
holder plate evenly against the face of the seal chamber
with the nuts, alternately tightening one and then the
other. This will compress the mechanical seal to correct
operating length and compress the plate gasket to seal
off the seal chamber.
17. Remove the tapered installation sleeve.
18. Place the inner end cap with lipseal (lip facing end of
shaft) on shaft.
19. Install the thrust bearing housing on end of the rotor
bearing sleeve and tighten the nuts and capscrews
securely.
It is not necessary to use a gasket between these parts.
20. Insert both tapered roller bearings in the thrust bearing
housing, large end of the inner races together.
CAUTION: It is possible to install bearings incorrectly.
For proper assembly, refer to Figure 17.
21. Install the bearing spacer collar on the shaft next to the
inner race of the roller bearing.
SECTION TSM 143 ISSUE E PAGE 11 OF 15
Page 12
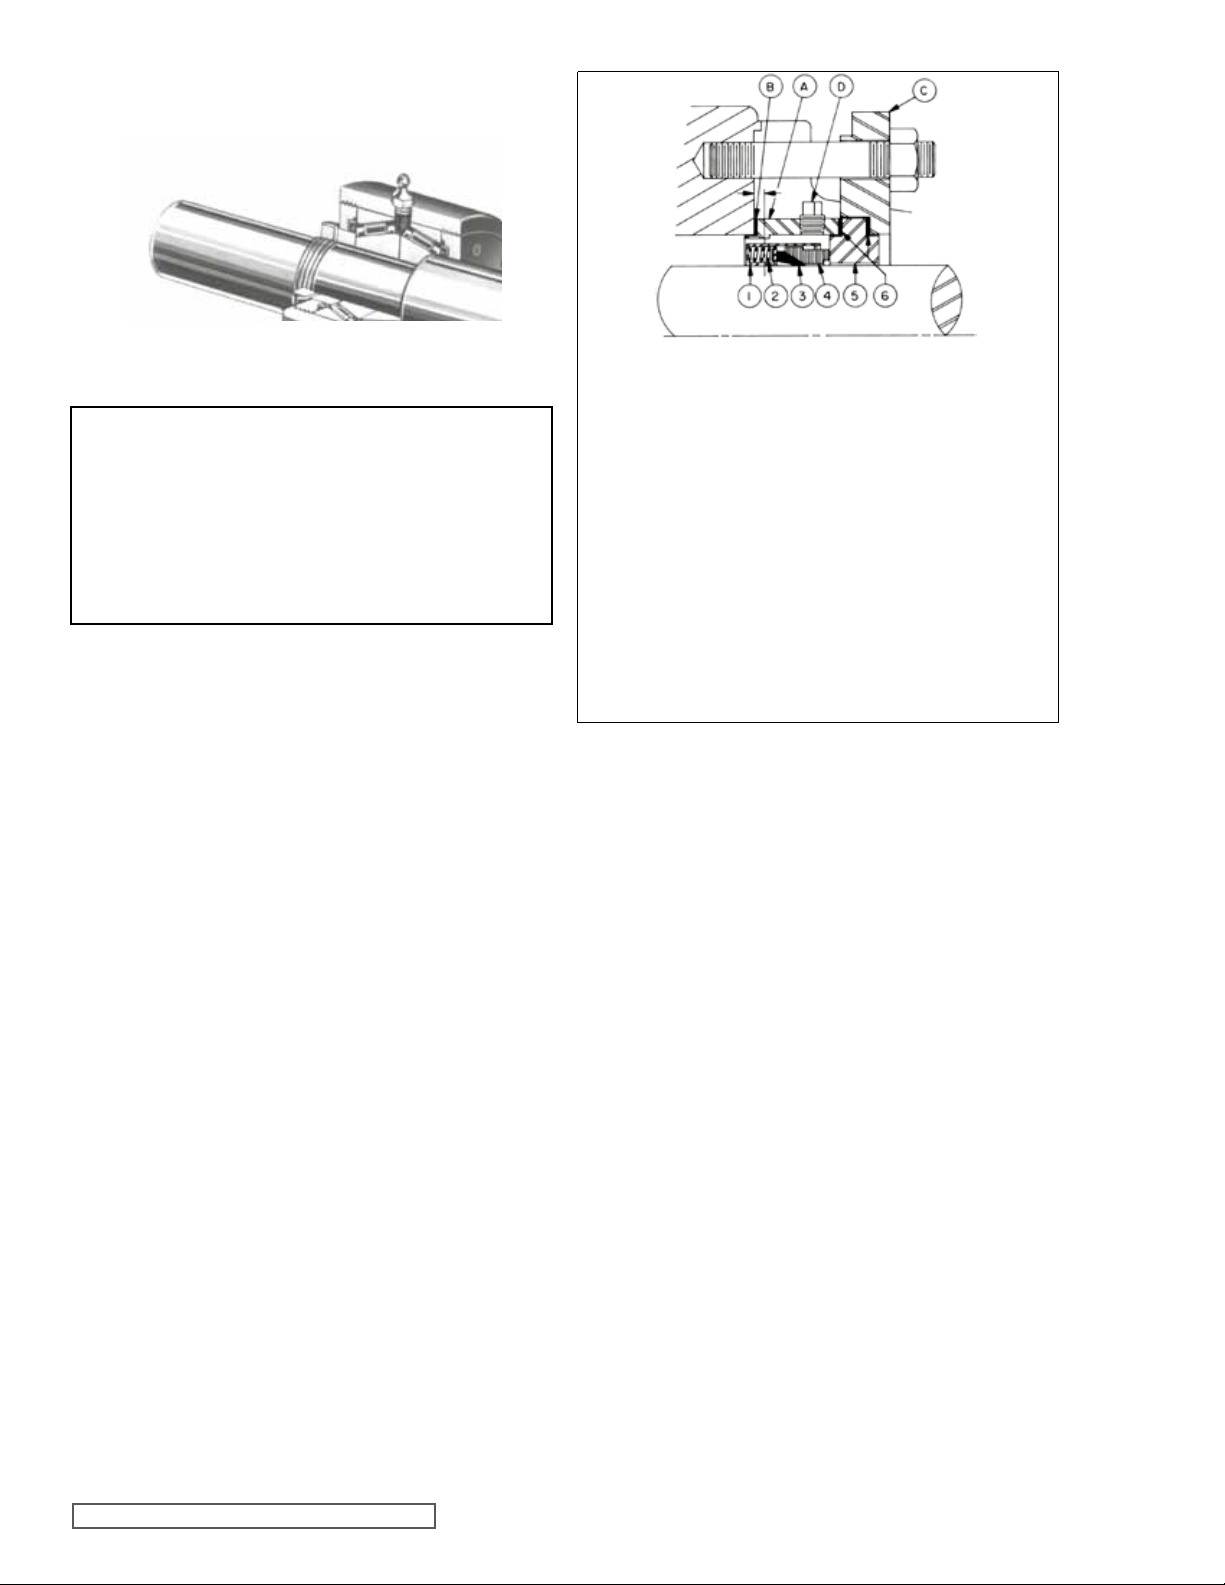
FIGURE 17
DANGER !
Before starting the pump, be sure all drive
equipment guards are in place.
Failure to properly mount guards may result in
serious injury or death
OPTIONAL MECHANICAL SEAL
(PTFE Fitted Type)
FIGURE 18
PTFE Fitted Mechanical Seal Assembly
For Models N-R4333, 4335 & 4337
1. Retainer Cartridge
2. Springs
3. PTFE Shaft Ring (wedge)
4. Rotating Face (washer)
5. Stationary Seal Seat
6. Seat Gaskets
Seal Mounting Parts
A. Packing box extension
B. Packing box extension gasket
C. Seal plate
D. Flush openings
DISASSEMBLY
Three components are furnished in the mechanical seal
assembly: Refer to Fgure 18, item numbers 1 thru 6.
1. The rotating assembly in which a retainer cartridge
encloses a spring loaded PTFE shaft ring and polished
rotating face. Set screws located around the outside of
the retainer cartridge are provided for securing rotating
assembly to pump shaft.
2. The stationary seal seat.
3. Two seal seat gaskets.
Three pump parts necessary for mounting PTFE mechanical
seal are illustrated in Figure 18, item letters A, B, C and D.
1. The packing box extension, has a machine pilot on the
end for installation in the rotor bearing sleeve and two
tapped holes for the seal flush.
2. The packing box extension gasket.
3. The seal plate is mthe achined to accept seal seat and
gasket.
1. Disassemble the pump per steps 1 thru 10 on page 8
under MECHANICAL SEAL DISASSEMBLY.
2. Remove the seal plate nuts from the studs and remove
the seal plate, gaskets and stationary seat.
3. If the pump is equipped with a flush line, disconnect
from the packing box extension.
4. Remove the packing box extension and gasket.
5. Loosen the set screws in the mechanical seal retainer
cartridge and remove from the rotor shaft. Refer to
Figure 18.
ASSEMBLY
1. Reassemble the pump per steps 1 thru 9 on pages 10
& 11, under ASSEMBLY, STANDARD MECHANICAL
SEAL. Step 1 (deburring shaft) is very critical prior to
the seal assembly.
NOTE: The tapered installation sleeve is available from
factory, at additional cost, for the N & R size pumps.from
Viking Pump Division.
2. Coat the large diameter of shaft, tapered sleeve, and
inside diameter of seal with non-detergent SAE 30
weight oil.
SECTION TSM 143 ISSUE E PAGE 12 OF 15
Page 13
3. Place the tapered installation sleeve (if on hand) and
install the seal on the shaft over tthe apered sleeve.
Position the seal on the shaft inside the rotor bearing
sleeve bore with end of seal located .19 inch inside
the machined face of the rotor bearing sleeve. Refer to
Figure 18.
4. Tighten all the seal drive set screws securely to the
shaft.
5. Remove the tapered installation sleeve.
6. Place the gasket on the packing box extension and
install the extension with the machined pilot inside the
rotor bearing sleeve bore.
7. Place the seat gasket over the shoulder of the stationary
seal seat and insert seat into the seal plate. Place the
remaining seat gasket over shoulder of polished surface
of stationary seat. Refer to Figure 18.
8. Place the seal plate with the stationary seat over the
mounting the studs and push the shoulder of stationary
seat into the packing box extension, the polished face
against the carbon rotating face.
9. Install the nuts on mounting studs and against seal
holder. Tighten the nuts evenly so the seal plate
and stationary seat will not be distorted when seal is
compressed.
10. Reassemble flush line to packing box extension.
AT THIS POINT, FINISH ASSEMBLY PROCEDURES
STARTING AT STEP 18, page 10.
THRUST BEARING ADJUSTMENT
Loosen the capscrews retaining the end cap locks on both
the inner and outer end caps. Slide the end cap locks out
far enough so the pins are no longer in the end cap retaining
holes. Using the spanner wrench provided with the pump,
turn the inner end cap towards the pump. Turn the outer
end cap in until the rotor shaft cannot be turned. With grease
pencil or chalk, make a reference mark on the bearing
housing OD and outer end cap. Back off the outer end cap
approximately 4 holes. One hole is equivalent to .005 inch
end clearance. Align the nearest end cap hole with the outer
end cap lock. Tighten the setscrew holding this lock. Tighten
the inner end cap until it is snug. Do not over tighten. Back
off slightly to align the nearest end cap hole with the end cap
lock. Tighten this setscrew. It is important not to tighten the
inner end cap to make the end cap lock align. This will cause
the tapered roller bearings to run too tightly and heat up.
Turn the rotor shaft to make sure it turns freely. If not, repeat
the above procedure.
Pumps built for viscous liquid or high temperature service
may require extra end clearance. Each hole on the end
cap is about .004 inch additional end clearance. Consult
an authorized Viking distributor or the factory for further
information.
INSTALLATION OF CARBON
GRAPHITE BUSHINGS
When installing carbon graphite bushings, extreme care
must be taken to prevent breaking. Carbon graphite is a
brittle material and easily cracked. If cracked, the bushing will
quickly disintegrate. Using a lubricant and adding a chamfer
on the bushing and the mating part will help with installation.
The additional precautions listed below must be followed for
proper installation.
1. A press must be used for installation.
2. Be certain the bushing is started straight.
3. Do not stop the pressing operation until the bushing is in
the proper position; starting and stopping will result in a
cracked bushing.
4. Check the bushing for cracks after installation.
Carbon graphite bushings with extra interference fits are
frequently furnished for high temperature operation. These
bushings must be installed by a shrink fit.
1. Heat the rotor bearing sleeve or idler to 750º F.
2. Install cool bushings with a press.
3. If facilities are not available to reach 750º F. temperature,
it is possible to install with 450º F. temperature; however,
the lower the temperature, the greater the possibility of
cracking the bushing.
Consult factory with specific questions on high temperature
applications. Refer to Engineering Service Bulletin ESB-3.
Standard catalog pumps require the following end clearance
settings.
Pump Size Standard End Clearance (Inch)
N .015
R .020
P .025
SECTION TSM 143 ISSUE E PAGE 13 OF 15
Page 14
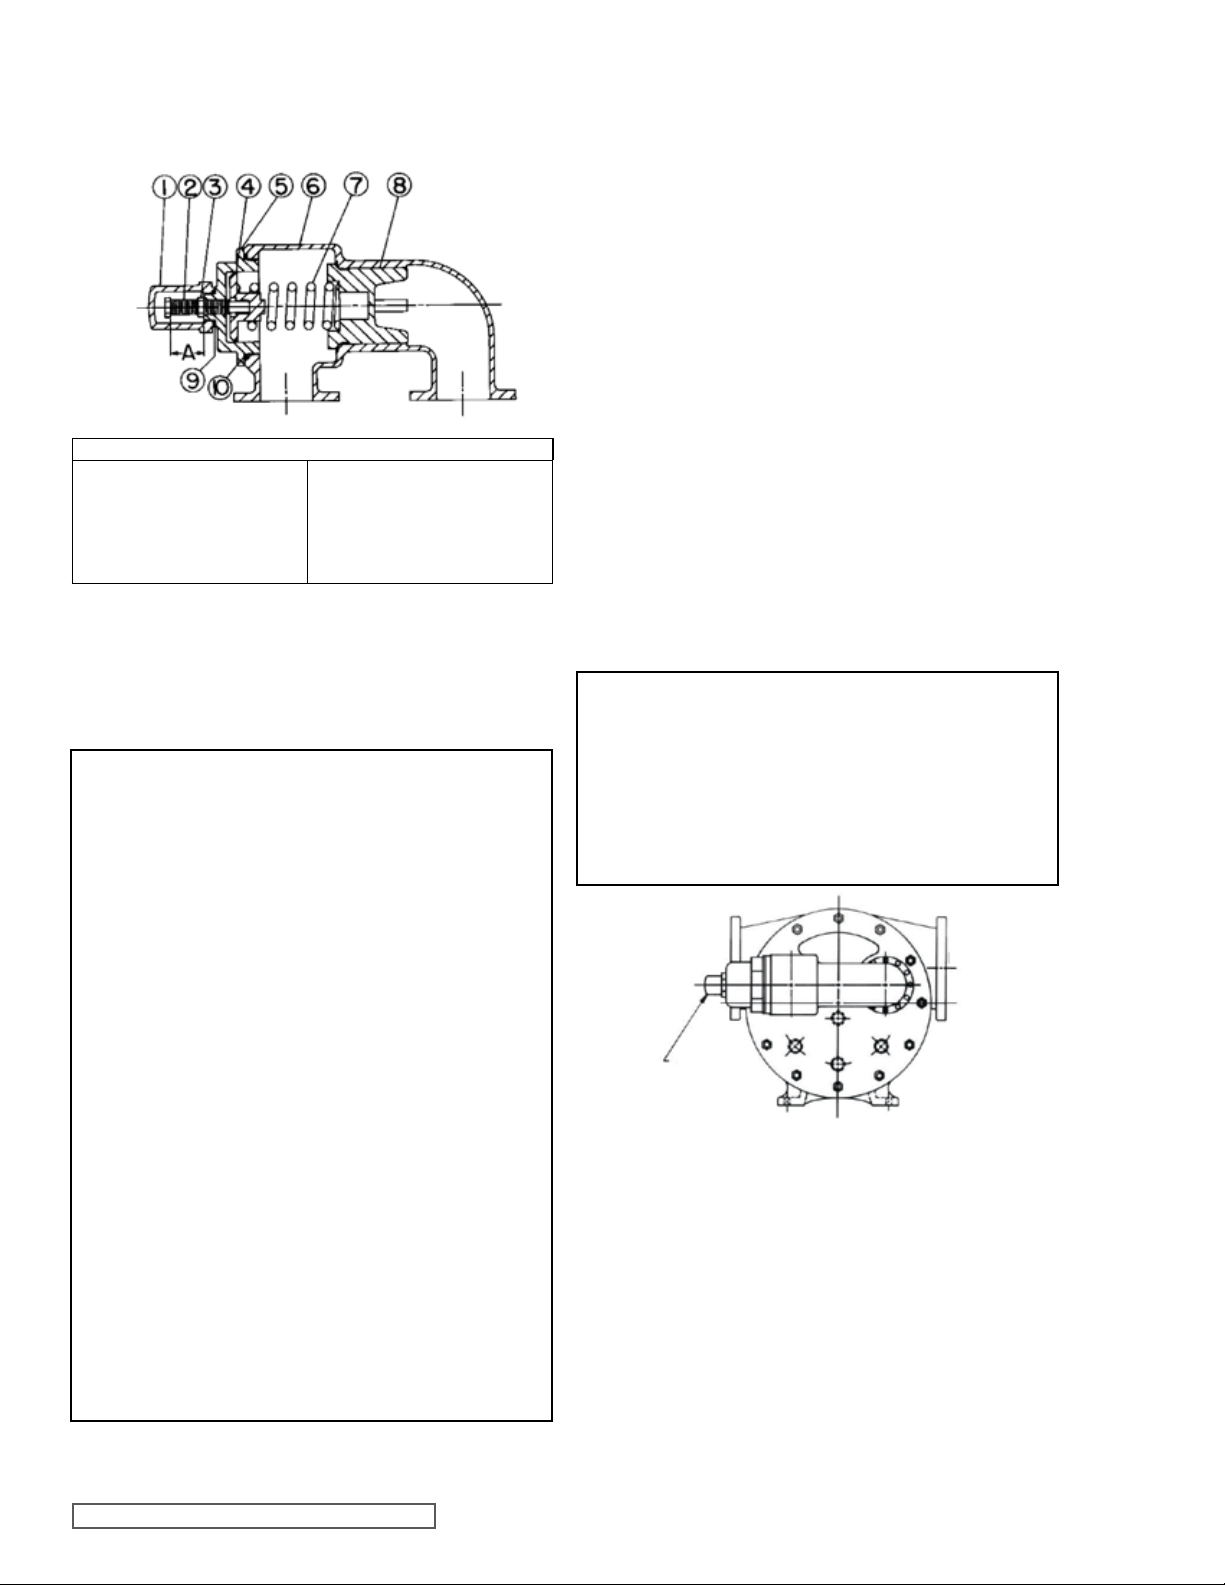
PRESSURE RELIEF VALVE INSTRUCTIONS
Mark valve and head before disassembly to ensure proper
reassembly.
1. Remove the valve cap.
2. Measure and record the length of extension of adjusting
screw. Refer to “A” on Figure 19.
3. Loosen the locknut and back out the adjusting screw
until the spring pressure is being released.
4. Remove the bonnet, spring guide, spring and poppet
from the valve body. Clean and inspect all parts for wear
and damage and replace as necessary.
LIST OF PARTS
1. Valve Cap
2. Adjusting Screw
3. Lock Nut
4. Spring Guide
5. Bonnet
6. Valve Body
7. Valve Spring
8. Poppet
9. Cap Gasket
10. Bonnet Gasket
FIGURE 19
DISASSEMBLY
DANGER !
Before opening any Viking pump liquid chamber (pumping chamber, reservoir, relief valve
adjusting cap fitting etc.) Be sure:
1. That any pressure in the chamber has been
completely vented through the suction
or discharge lines or other appropriate
openings or connections.
ASSEMBLY
Reverse the procedures outlined under DISASSEMBLY. If
the valve is removed for repairs, be sure to replace in the
same position.The relief valve adjusting screw cap must
always point towards suction side of the pump. If the pump
rotation is reserved, remove the relief valve and turn end for
end. Refer to Figure 20.
DANGER !
Before starting the pump, be sure all drive
equipment guards are in place.
Failure to properly mount guards may result in
serious injury or death.
INLET
OR
SUCTION
OUTLET
OR
DISCHARGE
2. That the driving means (motor, turbine,
engine, etc.) Has been “locked out” or made
non- operational so that it cannot be started
while work is being done on pump.
3. That you know what liquid the pump
has been handling and the precautions
necessary to safely handle the liquid.
Obtain a material safety data sheet (MSDS)
for the liquid to be sure these precautions
are understood.
Failure to follow the above listed precautionary measures may result in serious injury or
death.
SECTION TSM 143 ISSUE E PAGE 14 OF 15
RELIEF VALVE
ADJUSTING
SCREW CAP
FIGURE 20
PRESSURE ADJUSTMENT
If a new spring is installed or if the pressure setting of the
pressure relief valve is to be changed from that which the
factory has set, the following instructions must be carefully
followed.
1. Carefully remove the valve cap, which covers the
adjusting screw.
Loosen the locknut, which locks the adjusting screw so
the pressure setting will not change during operation of
pump.
Page 15
TECHNICAL SERVICE MANUAL
2. Install a pressure gauge in the discharge line for the
actual adjustment operation.
3. Turn the adjusting screw in to increase pressure and out
to decrease pressure.
4. With the discharge line closed at a point beyond pressure
gauge, the gauge will show maximum pressure valve will
allow while pump is in operation.
IMPORTANT
When ordering parts for the pressure relief valve, always give
the model number and serial number of pump as it appears
on the nameplate and name of part wanted. When ordering
springs, be sure to give the pressure settings desired.
SECTION TSM 143
HEAVY DUTY PUMPS
SERIES 335 AND 4335
PAGE 15 OF 15
ISSUE E
SIZES N, R, AND P
WARRANTY
Viking warrants all products manufactured by it to be
free from defects in workmanship or material for a
period of one (1) year from date of startup, provided
that in no event shall this warranty extend more than
eighteen (18) months from the date of shipment from
Viking. The warranty period for Universal Seal series
pumps ONLY (Universal Seal models listed below) is
three (3) years from date of startup, provided that in
no event shall this warranty extend more than forty-two
(42) months from the date of shipment from Viking.
UNDER NO CIRCUMSTANCES SHALL VIKING BE
LIABLE UNDER THIS WARRANTY OR OTHERWISE
FOR SPECIAL, INCIDENTAL, INDIRECT,
CONSEQUENTIAL OR PUNITIVE DAMAGES OF ANY
KIND, INCLUDING, BUT NOT LIMITED TO, LOST
OR UNREALIZED SALES, REVENUES, PROFITS,
INCOME, COST SAVINGS OR BUSINESS, LOST OR
UNREALIZED CONTRACTS, LOSS OF GOODWILL,
DAMAGE TO REPUTATION, LOSS OF PROPERTY,
LOSS OF INFORMATION OR DATA, LOSS OF
PRODUCTION, DOWNTIME, OR INCREASED
COSTS, IN CONNECTION WITH ANY PRODUCT,
EVEN IF VIKING HAS BEEN ADVISED OR PLACED
ON NOTICE OF THE POSSIBILITY OF SUCH
DAMAGES AND NOTWITHSTANDING THE FAILURE
OF ANY ESSENTIAL PURPOSE OF ANY PRODUCT.
THIS WARRANTY IS AND SHALL BE VIKING’S SOLE
AND EXCLUSIVE WARRANTY AND SHALL BE IN
LIEU OF ALL OTHER WARRANTIES, EXPRESS
OR IMPLIED, INCLUDING, BUT NOT LIMITED
TO, ALL WARRANTIES OF MERCHANTABILITY,
FITNESS FOR A PARTICULAR PURPOSE AND
NON-INFRINGEMENT ALL OF WHICH OTHER
WARRANTIES ARE EXPRESSLY EXCLUDED.
See complete warranty at www.vikingpump.com.
VIKING PUMP, INC. • A Unit of IDEX Corporation • Cedar Falls, IA 50613 USA
© 3/2013 Viking Pump Inc.
All rights reserved
 Loading...