

Page 1
INSTALLATION, OPERATION AND MAINTENANCE MANUAL (IOM)
Model 5400 Pilot Operated
Pressure Relief Vent
IOM-5400
02-16
ISO Registered Company
SECTION I
I. DESCRIPTION AND SCOPE
The maintenance of this Pilot Operated Vent Valve
(POVV) should only be done by qualified valve
technicians. It is important that the technician be
familiar with the API and corporate standards,
corporate safety policies and the relief vent
manufacturer requirements. When repair services
are performed by an outside company, the company
needs to be a Cashco factory authorized repair
center which specializes in low pressure venting
devices.
SECTION II
II. VALVE DESIGN AND FUNCTION
The Model 5400 Pilot Operated Vents are used on
liquid storage tanks and other process vessels or
systems to prevent structural damage due to excess
internal pressure. This excess pressure is vented to
the atmosphere.
Storage tanks are pressurized when liquid is
pumped in, compressing the existing vapor, or
when increasing temperature causes increased
evaporation or expansion of existing vapor.
Conversely, a vacuum may be created when fluid
is pumped out or as atmospheric temperature
decreases. To prevent structural damage, vapor
must be allowed to escape or enter the tank at a
specified flow rate. The volume rate of venting is
dependent on the tank size, displacement rate and
the flash point of the fluid. See API Standard 2000
for procedures to determine venting requirements.
A pilot operated relief vent has two principal
advantages over other relief vent designs:
1. Bubble tight shutoff up to 100% of set point.
2. Full open capacity for pressure relief is achieved
within 10% above set point.
For information on repair centers in your area,
please contact:
Valve Concepts, Inc.
%Cashco, Inc.
607 West 15th Street
Ellsworth, KS 67439-0006
(785) 472-4461 (Phone)
(785) 472-3539 (Fax)
Thus the vent valve is capable of operating at
pressures closer to the maximum allowable
working pressure of the tank. Operating at higher
pressures reduces evaporation and total venting
volume, thereby reducing product loss and the cost
of handling emissions.
Each application must be reviewed to ensure material compatibility with all metal and soft good
components with the service conditions. The pallet
assembly, wetted components and tubing are 316
SST. Diaphragm material is FKM, unless specified
otherwise.
The pilot valve is factory set to comply with the
specifications on the purchase order. The adjustable pressure range is a function of the installed
spring and will be stamped on the metal nameplate.
The set point pressure may be changed within the
design parameters of the spring while installed on
line or in a maintenance shop. See Section IX for
setting and testing procedures.
This manual is intended to provide recommended
procedures and practices for installation, operation
and maintenance of the Model 5400 POVV. Although this manual cannot cover all possible contingencies, these guidelines will provide safe and
reliable pilot valve performance.
Page 2
SECTION III
III. SAFETY WARNINGS
WARNING
Warning: Before beginning any relief vent inspection
or maintenance, carefully read and understand the
information in this manual. If there are any questions
concerning the information in this manual, please
contact the factory before proceeding.
Tank or system protection is the primary function of
the Pilot Operated Vent Valve (POVV). It must be
selected to meet the total pressure flow requirements
within the maximum allowable working pressure
of the system on which it is installed. Consult API
Standard 2000 for tank protection sizing procedures.
Improperly specified relief vents may result in
structural damage to the tank or system, and can
cause severe personal injury or death.
In the event of a diaphragm failure, the Model 5400
will vent pressure to the atmosphere causing the
pressure relief vent to fail in the OPEN position. The
vent will function like a weight loaded valve under
this condition with a lower set point. Consult the
factory for any questions related to this over-pressure
condition.
The 1/2” OD SST pilot valve sensing line must be
kept open and unobstructed to ensure that the pilot
“senses” the actual tank pressure. For applications
where tank vapors may condense or polymerize in
the sensing tubing or the pilot valve, a nitrogen purge
may be required to prevent internal obstruction of the
tube. Consult the factory for recommendations.
CAUTION
DO NOT attempt to remove the vent from the tank or
process vessel without fi rst bleeding all pressure from
the system. ALTERNATIVE MEANS OF PRESSURE
RELIEF MUST BE PROVIDED WHEN THE VENT IS OUT
OF SERVICE.
After isolating the relief vent, bleed all pressure
from both main and pilot valve before removing the
Model 5400 POVV.
NOTE: Both the pilot valve and main valve are
exposed to the process vapors. Observe all
plant procedures and Material Safety Data Sheet
recommendations before inspecting, adjusting or
servicing any components.
CAUTION
DO NOT attempt to change pressure set point beyond
the limit specified on the nameplate.
SECTION IV
IV. SHIPPING, INSPECTION AND
STORAGE
The pressure relief vent is carefully packaged to
prevent damage or contamination during shipping.
Inspect the equipment when it is received and
report any damage to the carrier immediately. The
POVV should be stored in a clean environment with
all the protective flange covers in place to prevent
intrusion of foreign materials. If there are indications
of physical damage or internal contamination, the
valve may need to be disassembled, cleaned, and
inspected prior to installation.
The vent on the spring bonnet of the pilot must
be clean and unobstructed for proper and safe
operation of the valve.
Lifting brackets may be provided on the main valve
for lifting and handling. To avoid damage to the
lower flange surface, rest the vent on soft, clean
gasket material until it is ready to be installed. DO
NOT store the POVV directly on the ground.
2
IOM-5400
Page 3
V. INSTALLATION
SECTION V
The Model 5400 POVV is a precision device that
must be handled carefully to ensure seat tightness.
WARNING
The vent must be installed in a vertical position. The
tank nozzle on which the vent is mounted should have
the same nominal diameter as the venting device. It
is recommended that the tank nozzle flange face be
within 1 degree of horizontal for best performance of
the venting device.
1. At installation, the POVV should be carefully
lifted into position using the lifting lugs on the
body. Use the weather hood to help align the
body directly over the tank nozzle. DO NOT
use the pilot valve or pickup line to pull the
POVV into position.
2. Aluminum valve body should be mated to
flat-faced 125# ASME flanges. Mating flanges
should be flat (within 0.020”), clean, and free
of scratches, corrosion and tool marks. A full
faced gasket is recommended.
4. Center the gasket within the bolt circle of the
tank nozzle flange.
5. Lubricate all studs and nuts with an appropriate
thread lubricant. If stainless steel studs and
nuts are required, use an anti-seize lubricant
such as moly-disulfide.
6. Remove flange protective cover and carefully
set the POVV down on the gasket and face of
the nozzle flange.
WARNING
Minimum clearance between tank roof and vacuum
inlet port must be at least equal to the vents’
nominal flange bore. Tank nozzle bore must be
greater than or equal to vent inlet flange bore. Inlet
piping loads must be supported by appropriate
structural supports, NOT by the vent body.
7. Install lockwashers and nuts. Tighten nuts
to half the recommended torque value using
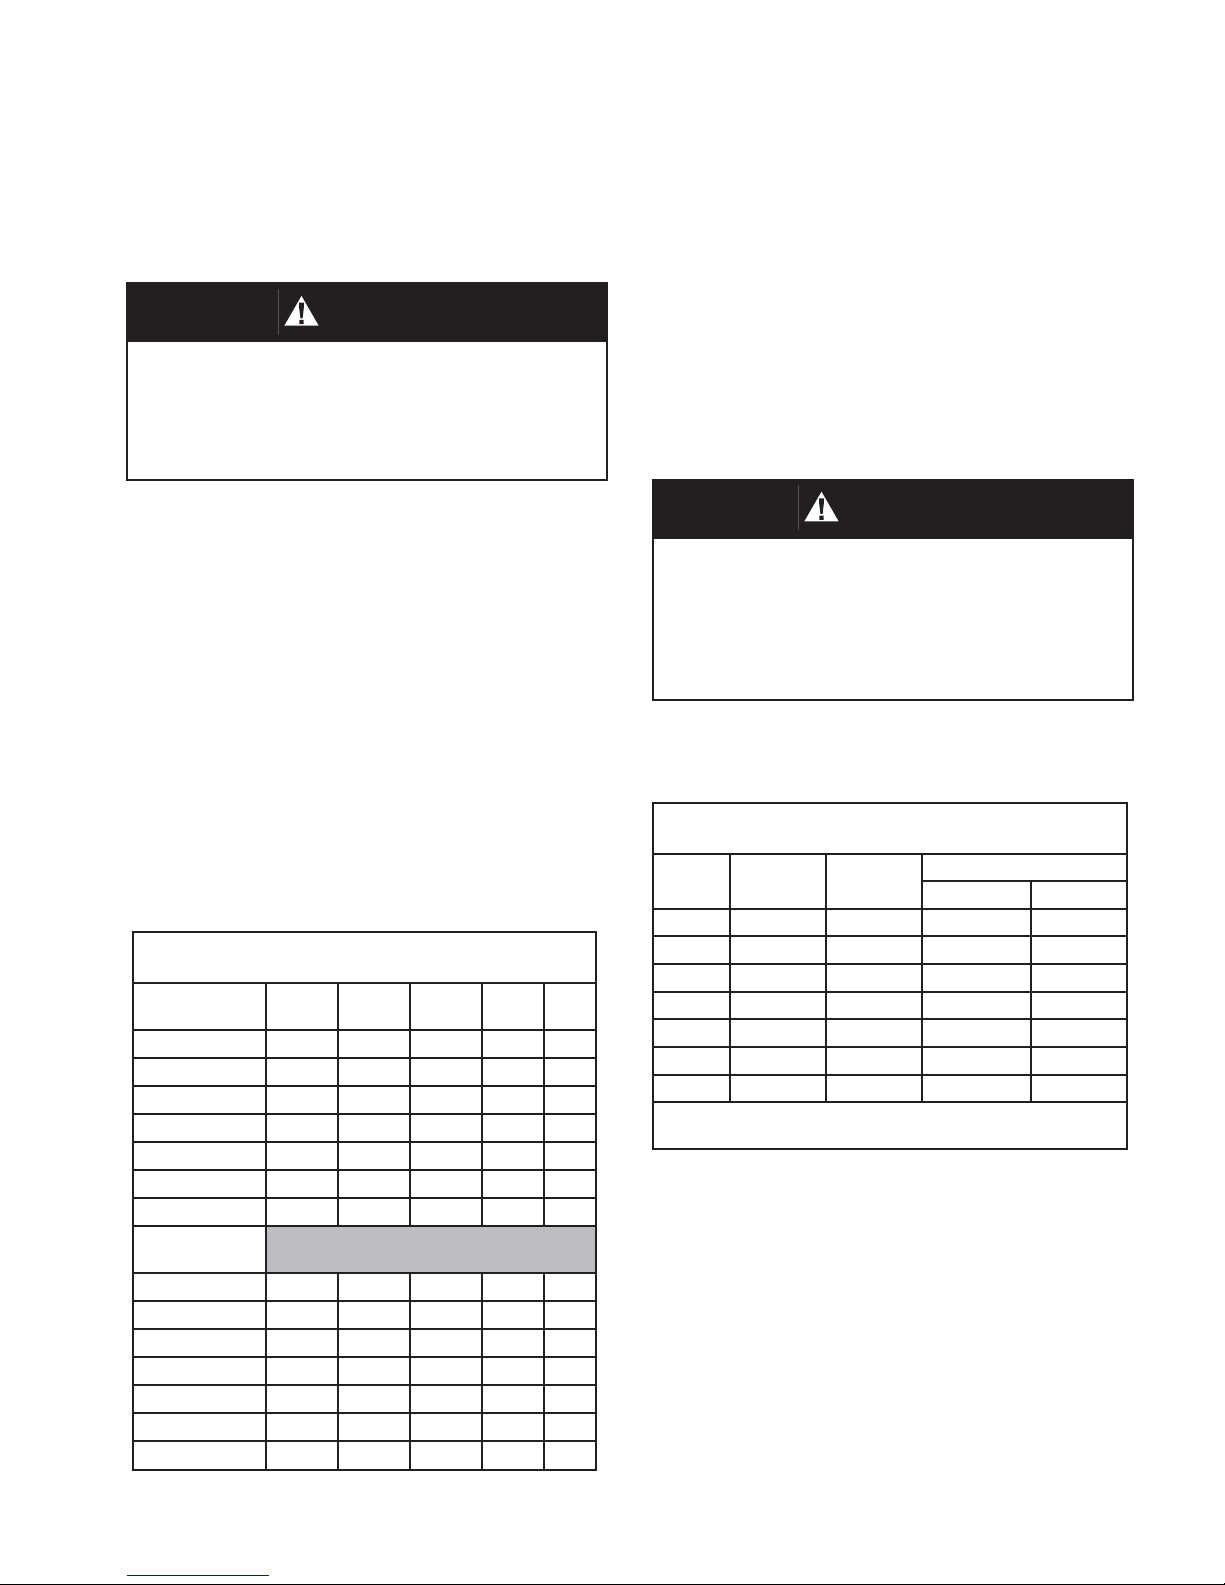
an alternating crossing pattern. See Table 2.
3. Install the flange gasket on the nozzle face.
Use either a full faced or ring gasket for
raised face flanges. Ensure that the gasket
material is suitable for the service. See Table
1 for gasket dimensions.
Table 1
Body Flange Gasket Dimensions
CS, SST
150# ASME RF
2’ 4.12 2.38 -- -- --
3” 5.38 3.50 -- -- --
4” 6.88 4.50 -- -- --
6” 8.75 6.62 -- -- --
8” 11.00 8.62 -- -- --
10” 13.38 10.80 -- -- --
12” 16.12 12.80 -- -- --
Alum w/ 125#
ASME FF
2” 6.00 2.00 4.75 .75 4
3” 7.50 3.00 6.00 .75 4
4” 9.00 4.00 7.50 .75 8
6” 11.00 6.00 9.50 .88 8
8” 13.50 8.00 11.75 .88 8
10” 16.00 10.0 14.25 1.00 12
12” 19.00 12.00 17.00 1.00 12
O.D. I.D. B.C. Hole Qty
Table 2
Recommended Minimum Torque Values *
Size
2” 4 5/8”-11 31 81
3” 4 5/8”-11 43 106
4” 8 5/8”-11 29 68
6” 8 3/4’10 51 101
8” 8 3/4”-10 78 142
10” 12 7/8”-9 75 138
12” 12 7/8”-9 93 179
* Torque values are based on a gasket factor m = 3.5,
gasket factor y = 4000 psi, operating pressure = 30 psi
Qty
Holes
Bolt
(UNC)
Torque (lb-ft)
Raised Face Flat Face
8. Make sure that the gasket is compressed
evenly and the flanges are not distorted.
NOTE: Misalignment of flange faces will
cause bending stresses at the flange and may
damage flange joint. Reference Addendum A
on pages 15-16.
9. Finish tightening nuts to the point that no
additional rotation occurs.
IOM-5400
3
Page 4
SECTION VI
VI. PILOT MAINTENANCE
A. General:
1. Maintenance procedures herein after are
based upon removal of the pilot/vent valve
unit from the vessel/piping where installed.
2. Owner should refer to owner’s procedures for
re mov al, handling and cleaning of non re us able parts; i.e. gaskets, suitable solvents,
etc.
3. All indicated Item Numbers that are with
respect to the Pilot Assembly will be in
pa ren the sis and un der scored; i.e. (29). All
Item Numbers that are with respect to the
MainValve are not un der scored; i.e. (107).
B. Separation from Main Valve and Disassembly:
1. Disconnect sense tube (127) from sense
tube connectors (125) and (126). Remove
the pilot valve assembly from the nipple
(124) by rotating the pilot body (01) CCW.
2. Secure pilot body (01) in vise with ‘sensing” port facing front. Disconnect tubing
(34) from connectors (32),(33).
3. Paint or embed a set of match marks between upper case (22), spacer (13) and
lower case (03) along flanged area. Note
the location of 1/8” NPT tap from elbow
(33) in relation to body sensing port and
straight connector (32).
WARNING
6. Lift range spring (20) and spring button
(21) up and set aside.
7. Insert a tool in the slot in the top of stud
(18) to prevent stud rotation. Rotate nut
(19) CCW to remove nut and spring guides
(17).
8. Remove sense pressure ring (15), sense
support plate (16), sense diaphragm (14)
and diaphragm case spacer (13).
9. Remove top bolt gasket (07), and sense
diaphragm spacer (12).
10. Remove boost support plate (11), boost
diaphragm (10), boost diaphragm spacer
(09) and bolt gasket (07).
FOR Pilot with Pressure > 3.2 psig:
remove boost pressure ring (36).
11. Rotate 7/16” hex head cap screws (04)
CCW to remove. Lift up on lower diaphragm
case (03) to remove lower case and body
gasket (02). NOTE the alignment of the
four bolt holes and the sense hole in case
(03) with the holes in the body (01).
12. Grasp spindle stud (18) and lift upwards to
extract the spindle assembly (06) from the
body (01). Remove seal diaphragm (08)
from spindle. With a pick type tool lift out
seat o-ring (05).
13. Rotate jam nut (27) CCW two rotations
and remove blowdown needle (28) from
body (01). Replace with new O-ring (30).
SPRING UNDER COMPRESSION. Prior to re mov ing
flange bolts, relieve spring com pres sion by backing
out the adjusting screw. Failure to do so may result
in flying parts that could cause personal injury.
4. Rotate the closing cap (29) CCW for
removal. Loosen the adjusting screw nut
(27) two revolutions. Rotate Adjusting
screw (28) CCW and remove.
5. Remove diaphragm case nuts (19),
washers (25), and cap screws (26).
Grasp spring bonnet (23) and lift up until
diaphragm case (22) clears top of spring
button (21). Set assembly aside.
4
14. Inspect parts and replace if parts show
signs of wear. Clean parts with suitable
cleaner.
C. Re-assembly:
1. Insert new seat o-ring (05) in the bottom
of the spindle assembly. Place spindle
assembly inside the body cavity, threaded
end up. Slide a new seal diaphragm over
threaded end of spindle and position it
on top of the body. Align holes in seal
diaphragm with holes in body.
IOM-5400
Page 5
2. Position new body gasket (02) on top of
the seal diaphragm, align gasket holes.
DO NOT cover sensing hole in the
body.
3. Align holes in the lower diaphragm case
(03) with body (01) and place the case
on top of the gasket. DO NOT cover
sensing hole. Use cap screws (04) to
secure lower diaphragm case (03) to the
body. (01). Tighten to 10-15 ft. lbs.
4. Slide one bolt gasket (07) and boost
diaphragm spacer (09) over threaded end
of spindle (18).
13. Lower the upper diaphragm case (22)
/ spring bonnet (23) assembly over the
spring (20), allow to rest on the diaphragm
ring (15). (Ensure alignment of match
marks per previous B 3.)
14. Install diaphragm case screws (26), flat
washers (25), and nuts (19) and tighten.
15. Apply a light coat of Bostik Never-Seez to
threads of blowdown needle (28). Thread
completely into body until the nut (27)
contacts the body (01) and then back
out two rotations. Rotate nut (27) CW to
secure nut tight.
5. Place another bolt gasket (07), the boost
diaphragm (10), and the support plateboost (11) on spindle stud (18). Align all
bolt holes for all parts.
FOR Pilot with Pressure > 3.2 psig:
install boost pressure ring (36).
6. Install sense diaphragm spacer (12) and
the last bolt gasket (07) on spindle stud
(18).
7. Place the diaphragm case spacer (13) on
the top of the diaphragm (or on top of the
boost pressure ring (36)) and align match
marks per previous B 3.
8. Install a new sense diaphragm (14) on
spindle stud (18) and align the bolt holes
with the boost diaphragm (10) and spacer
(13).
9. Stack the sense support plate (16) and
the spring guides (17) over end of spindle
stud (18).
16. Reinstall adjusting screw (28) and jam nut
(27) in top of spring bonnet (23). Install
closing cap (29).
17. Refer to Section IX for Calibration and
Testing.
18. Install pilot body assembly on nipple
(124) tight with CW rotation. Ensure the
sense tube connector (126) of the pilot
valve assembly is directly above sensing
tube connector (125) of the main valve
assembly.
19. Reconnect tubing (34) to fittings (32), (33)
and tubing (127) to fittings (125),(126).
10. Install and tighten nut (19) to secure all
parts. (Check alignment of the bolt holes
around the circumference.)
11. Position the range spring (20) and spring
button (21) on the spring guides (17).
12. Place pressure ring (15) on top of
diaphragm (14). Recheck alignment of
bolt holes.
IOM-5400
5
Page 6
SECTION VII
VII. VENT VALVE MAINTENANCE
CAUTION
If the vent valve must be removed from the tank for
any reason, make sure that all pressure has been released before the flange fasteners are loosened. Refer
to your company procedures before venting the tank
pressure and when handling toxic or otherwise hazardous materials. Observe all standard safety precautions as specified on Material Safety Data Sheets for
the product(s) in the system while removing the valve
and during the repair.
A. General:
1. The Model 5400 POVV does not require
routine lubrication or adjustments. It should
be checked periodically, at least twice a
year, to confirm that the valve is functioning
properly and that the set point is correct.
2. The pilot valve is designed to function in
a fail-safe manner. The failure of a seal
or a diaphragm will cause pressure to be
vented to the atmosphere; the resulting
loss in pressure will cause the main valve
to open under rising pressure.
3. Periodic inspection for seat tightness
should be done to ensure compliance with
local air pollution control requirements. If
the valve relieves to the atmosphere, this
may be accomplished with a gas detector
calibrated for the principle product in the
system.
4. The vent valve will need to be periodically
removed from the tank for inspection of
diaphragms, gaskets and seals. When this
is done, the vent must be handled carefully
using the lifting brackets and the body.
Actuator Diaphragm Replacement:
a. Paint or embed a set of match marks
between upper case (118) and lower case
(114) across the case flange edge.
b. Loosen and remove nuts (120) and cap
screws (119).
c. Lift up and remove the upper case
(118) assy and set aside. Remove joint
tape (129) and diaphragm (117). NOTE:
To continue with disassembly skip to
Pressure Pallet Diaphragm Replacement
below.
d. Replace with new parts (129 and
117). Position and align bolt holes in the
circumference of the diaphragm with the
holes in the lower case (114).
e. Reposition upper case assy (118) on
diaphragm (117). Align marks of a. above.
f. Install cap screws (119) and nuts (120)
and tighten.
g. Install pilot body assembly on nipple
(124) tight with CW rotation. Ensure
connector (126) of the pilot valve assembly
is directly above sensing tube connector
(125) of the main valve assembly.
h. Reconnect tubing (127) to fittings
(125),(126). Refer to Section IX for
Calibration and Testing.
Pressure Pallet Diaphragm replacement:
(Disassembly continues from c. above)
a. Paint or embed a set of match marks
between weatherhood (111) and body
(100).
5. The main and pilot valve housings, bodies,
pallet assembly and other components are
exposed to the process vapor.
B. Disassembly:
1. Disconnect the tubing connections (pilot
to main valve) (127, 125 and 126) and
remove the pilot by rotating the pilot body
(01) assembly CCW from nipple (124).
6
b. Rotate jam nuts (122) CCW coming
down to rest against top of jack screw (121).
Rotate jack nuts (123) CCW coming down
to rest against nuts (122).
c. Rotate jack screw (121) CCW and
remove from threaded end of pallet guides
(109).
d. Grasp case assy (AA) (114/118) and lift
straight up to remove (AA) and weatherhood
assy (111) from pallet guides (109).
IOM-5400
Page 7
CAUTION
Do not grasp weatherhood around the bottom edge, it
may be sharp.
NOTE: Support plate (116) will also slide off
pressure stem (103). (Continue on to
step i. unless changing gasket (113)).
To Replace Adapter Gasket: steps (e. - h).
e. Lay the (AA) and weatherhood assy on
flat surface, bottom edge of weatherhood
resting on flat surface. Grasp the top of
the support plate weldment and lift up to
remove.
surface) of the diaphragm (106).
n. Install the diaphragm retainer plate
(107) and lock nut (108), secure nut tight.
o. Remove pallet (105) assembly from
vise.
To Remove Seat Ring:
NOTE: If vent has integral or pressed in
seat rings, contact the factory.
Paint or embed a set of match marks
between the seat ring and the inside of the
body.
IOM-5400
f. Paint or embed a set of match marks
between weatherhood (111) and lower
actuator case assy (114).
g. Flip the weatherhood over so lower
case (114) is resting on the flat surface.
Loosen and remove adapter bolts (115).
Set weatherhood (111) to the side and
remove weatherhood plate (112). Remove
and replace actuator case gasket (113).
h. Align bolt holes in weatherhood plate
(112) and weatherhood (111) with lower
actuator case assy (114) and install
adapter bolts (115). Tighten securely.
i. Remove wire screen (110) from seat
ring. Lift pressure stem/pallet (103/105)
assembly straight up off the seat ring
(101). Inspect seating surface of seat
ring and pallet diaphragm (106) Inspect
seating surface of seat ring (101).
j. Carefully secure stem (103) in a vise
with lock nut (108) up. Remove nut from
pressure stem.
k. Remove diaphragm retainer plate
(107), diaphragm (106), pallet (105) and
stiffener plate (104) from stem.
l. Clean and inspect parts for wear,
replace if worn. Re-install stiffener plate
(104) and pallet (105) on stem. NOTE:
Apply small amount of TFE paste around
the center opening (top surface) of the
pallet.
m. Place a new diaphragm (107) on the
pallet (105). NOTE: Apply small amount of
TFE paste around the center opening (top
p. Rotate bolts (102) CCW and remove.
Place a wrench on the milled flats of the
pallet guides (109), rotate CCW to remove.
Mark the location of guides on the edge
of the seat ring (101) for reference at reassembly.
q. Lift up to remove seat ring (101) and
joint tape (129). (There is no tape on
integral or pressed in seat rings.) Inspect
guides (109) and inside cavity of the body
(100) for any corrosion or product build
up. Clean all parts as necessary. Seat
surfaces must be clean and smooth for
diaphragm and pallet to seal properly.
r. Install new joint tape down inside body.
Align match marks for seat ring (101) with
body, place seat ring back in body, resting
on joint tape. Re-install pallet guides (111)
around the seat ring as previously marked.
Install bolts (102). Tighten bolts (102) and
guides to 15 ft. lbs. (20.3 Nm).
s. Position bug screen (110) on top
surface of seat ring (101). Position stem/
pallet (103/105) assembly on seat ring
(101)
t. Lift the lower actuator case assembly
(AA) (114) with attached weatherhood
(111) up and place it over the pallet
guides (109). Align match marks between
weatherhood and body, as per previous
step a. Lower the weatherhood down on
pallet guides (109).
u. Insert small end of support plate (116)
down through the hole in the center of the
lower case (114) until it slides over the top
of the pressure stem (103).
7
Page 8
v. Install jack screw (121) on threaded
end of pallet guides and tighten securely.
in step B. 1. a. previous. Install cap screws
(119) and nuts (120) and tighten.
Rotate jack nut (123) CW in equal
increments until they rest tight against
lower case (114). Rotate jam nut (122) CW
to secure tight to jack nut (123).
y. Install pilot body assembly on nipple
(124) tight with CW rotation. Ensure
the straight connector (126) of the pilot
valve assembly is directly above sensing
w. Install new piece of joint tape and
diaphragm (129 and 117). Position and
tube connector (125) of the main valve
assembly.
align bolt holes in the circumference of the
diaphragm with the holes in the lower case
(114).
z. Reconnect tubing (127) to fittings
(125),(126).
x. Reposition upper case assy (118) on
diaphragm (117). Align match marks made
SECTION VIII
VIII. ORDERING INFORMATION
NEW REPLACEMENT UNIT vs PARTS "KIT" FOR FIELD REPAIR
To obtain a quotation or place an order, please retrieve the Serial Number and Product Code that was stamped
on the metal name plate and attached to the unit. This information can also be found on the Bill of Material
(“BOM”), a parts list that was provided when unit was originally shipped. (Serial Number typically 6 digits).
NEW REPLACEMENT UNIT:
Contact your local Cashco, Inc., Sales Rep re sen ta tive with the Serial Number and Product code. With
this information they can provide a quotation for a
new unit including a complete description, price
and availability.
PARTS "KIT" for FIELD REPAIR:
Contact your local Cashco, Inc., Sales Rep re sen ta tive with the Serial Number and Product
code. Identify the parts and the quantity required
to repair the unit from the “BOM” sheet that
was provided when unit was originally shipped.
NOTE: Those part numbers that have a quantity indi-
CAUTION
Do not attempt to alter the original construction of any
unit without assistance and approval from the factory.
All purposed changes will require a new name plate with
appropriate ratings and new product code to accommodate the recommended part(s) changes.
cated under "Spare Parts" in column "A” reflect
minimum parts required for inspection and
rebuild, - "Soft Goods Kit". Those in column “B”
include minimum trim replacement parts needed
plus those "Soft Goods" parts from column "A".
If the "BOM" is not available, refer to the crosssectional drawings included in this manual for
part identification and selection.
A Local Sales Representative will provide
quotation for appropriate Kit Number, Price
and Availability.
The contents of this publication are presented for informational purposes only, and while every effort has been made to ensure their accuracy, they are not to be
construed as warranties or guarantees, express or implied, regarding the products or services described herein or their use or applicability. We reserve the right to
modify or improve the designs or specifications of such product at any time without notice.
Cashco, Inc. does not assume responsibility for the selection, use or maintenance of any product. Responsibility for proper selection, use and maintenance of any
Cashco, Inc. product remains solely with the purchaser.
8
IOM-5400
Page 9
SECTION IX
IX. PRESSURE CALIBRATION AND
TESTING PROCEDURE FOR PILOT
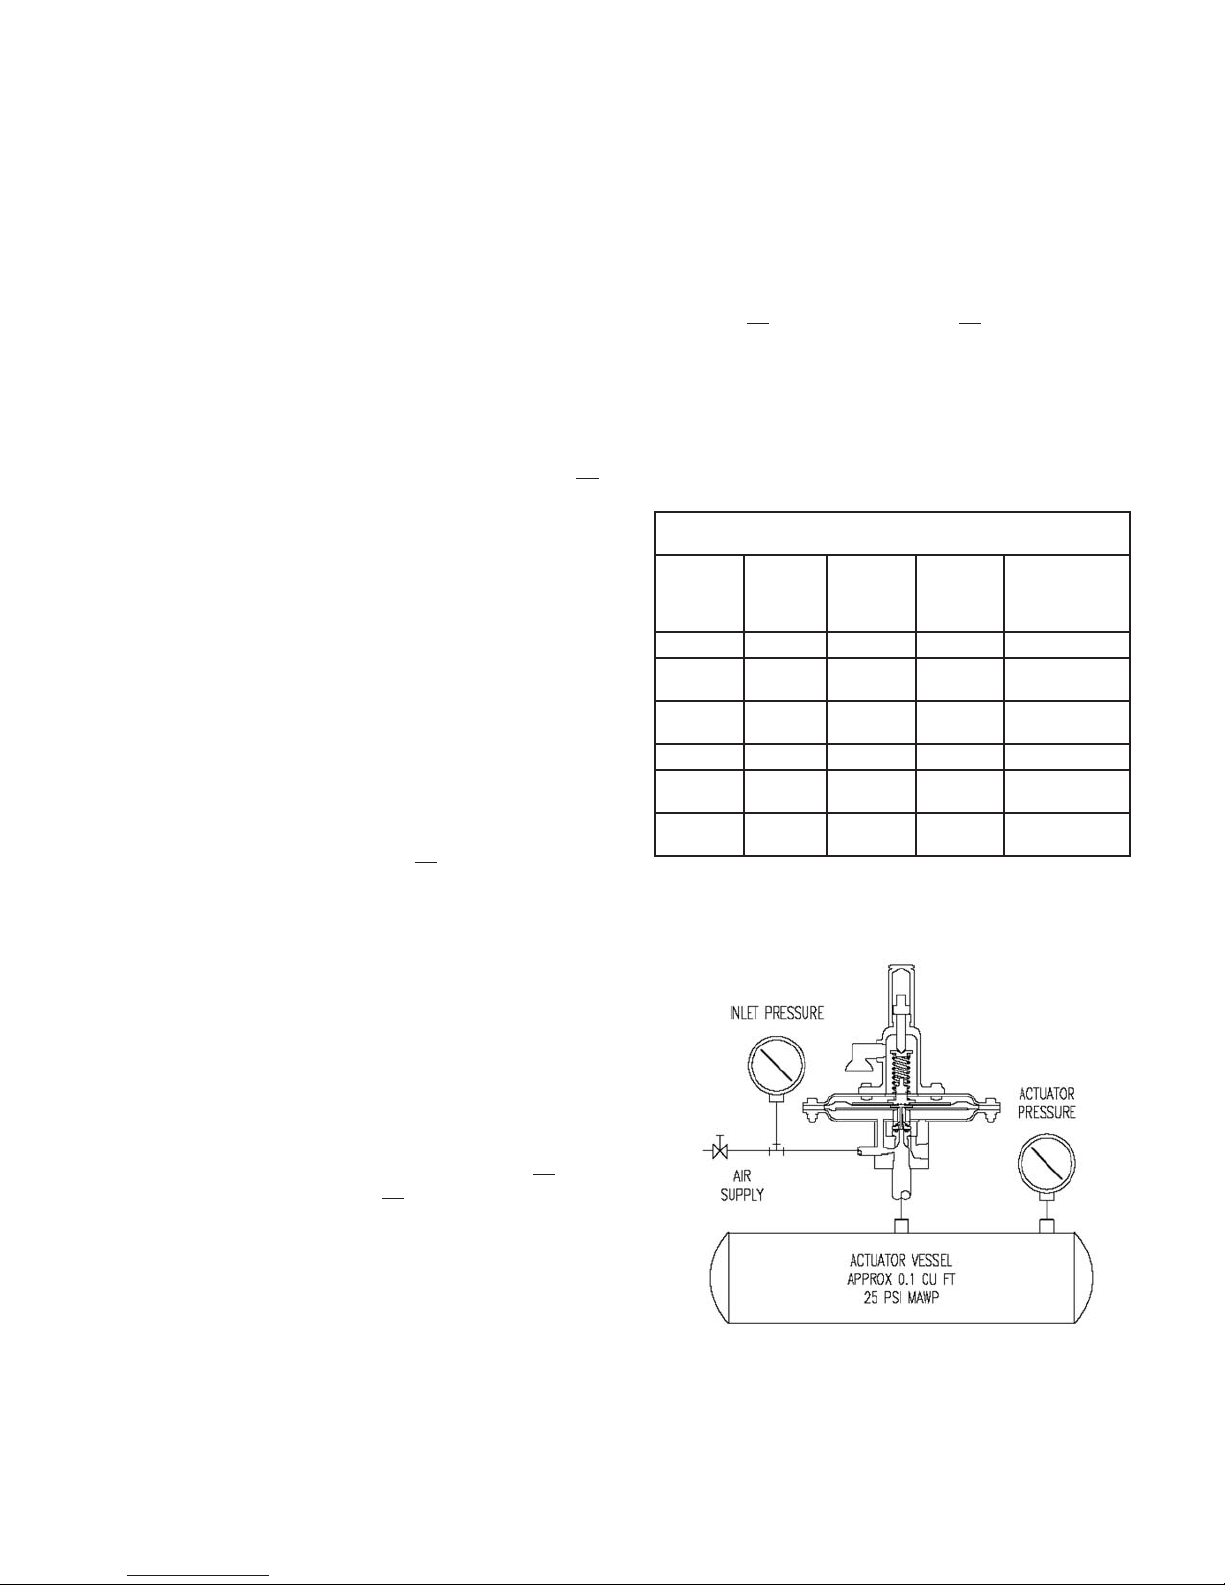
1. To determine set pressure, slowly increase
the pilot inlet pressure. Simulated actuator
pressure will rise with inlet. As set pressure
is approached, the actuator pressure will begin to decrease. Continue to increase the
inlet pressure slowly until the actuator pressure is 90% (+/- 10%) of the inlet pressure.
This is the set pressure.
2. Rotate the set pressure adjusting screw (28)
CW to increase set pressure or CCW to decrease set pressure. Continue to rotate the
adjusting screw and repeat the test per Step
1 previous until the specified set pressure is
achieved.
3. To determine reseat pressure, slowly decrease the inlet pressure and the actuator
pressure will begin to increase. Reseat occurs when the actuator pressure equal the
inlet pressure.
4. The difference between set and reseat
pressure,”blowdown”, can be adjusted with
the blowdown needle (28). Maximum clockwise rotation provides rapid relief valve opening, “snap action”’ and maximum blowdown.
Standard blowdown, unless otherwise specified is 7 - 10% below set pressure.
7. A small interaction occurs between set
pressure and blowdown adjustments. Readjustment of both may be required until
the specified set pressure and blowdown
are achieved. After completion, lock both
screws and locknuts and replace closing cap
(29) on adjusting screw (28).
8. Hold the valve at the set pressure while
preforming a soap bubble test of all bolted,
flanged and threaded connections.
9. Refer to Table 3 for standard setting Specifications.
SETTING SPECIFICATIONS - PILOT VALVE
Pilot Action
Snap 2” - 8” WC +/- 0.2”WC 75 90 +/- 3
Snap
Snap
Modulating 2” - 8” WC +/- 0.2” WC 75 100
Modulating
Modulating
Set
Pressure
8.1” WC -
1.0 psig
1.1 - 15.0
psig
8.1” - 1.0
psig
1.1 - 15.0
psig
TABLE 3
Set
Pressure
Limits
+/- 3% 90 90 +/- 3
+/- 3% 95 93 +/- 3
+/- 3% 90 100
+/- 3% 95 100
Maximum
Cracking
Pressure %
of Set
Reseat
Pressure
% of Set
FIGURE 1
Pilot Valve Test Stand
5. Increased counter clockwise rotation of
blowdown screw provides “modulating” action and minimum (zero) blowdown. Reseat
pressure is the same as set pressure.
NOTE: The blowdown needle is located
in a pressure containing chamber, and is
retained by the blowdown o-ring (30) and
blowdown locknut (27). DO NOT remove the
blowdown needle while under pressure.
6. Remove body vent and install a flexible tube
in this port. Immerse this pilot discharge
bubble tube in water approximately 1/4” below surface to detect cracking and reseat
pressure.
IOM-5400
9
Page 10
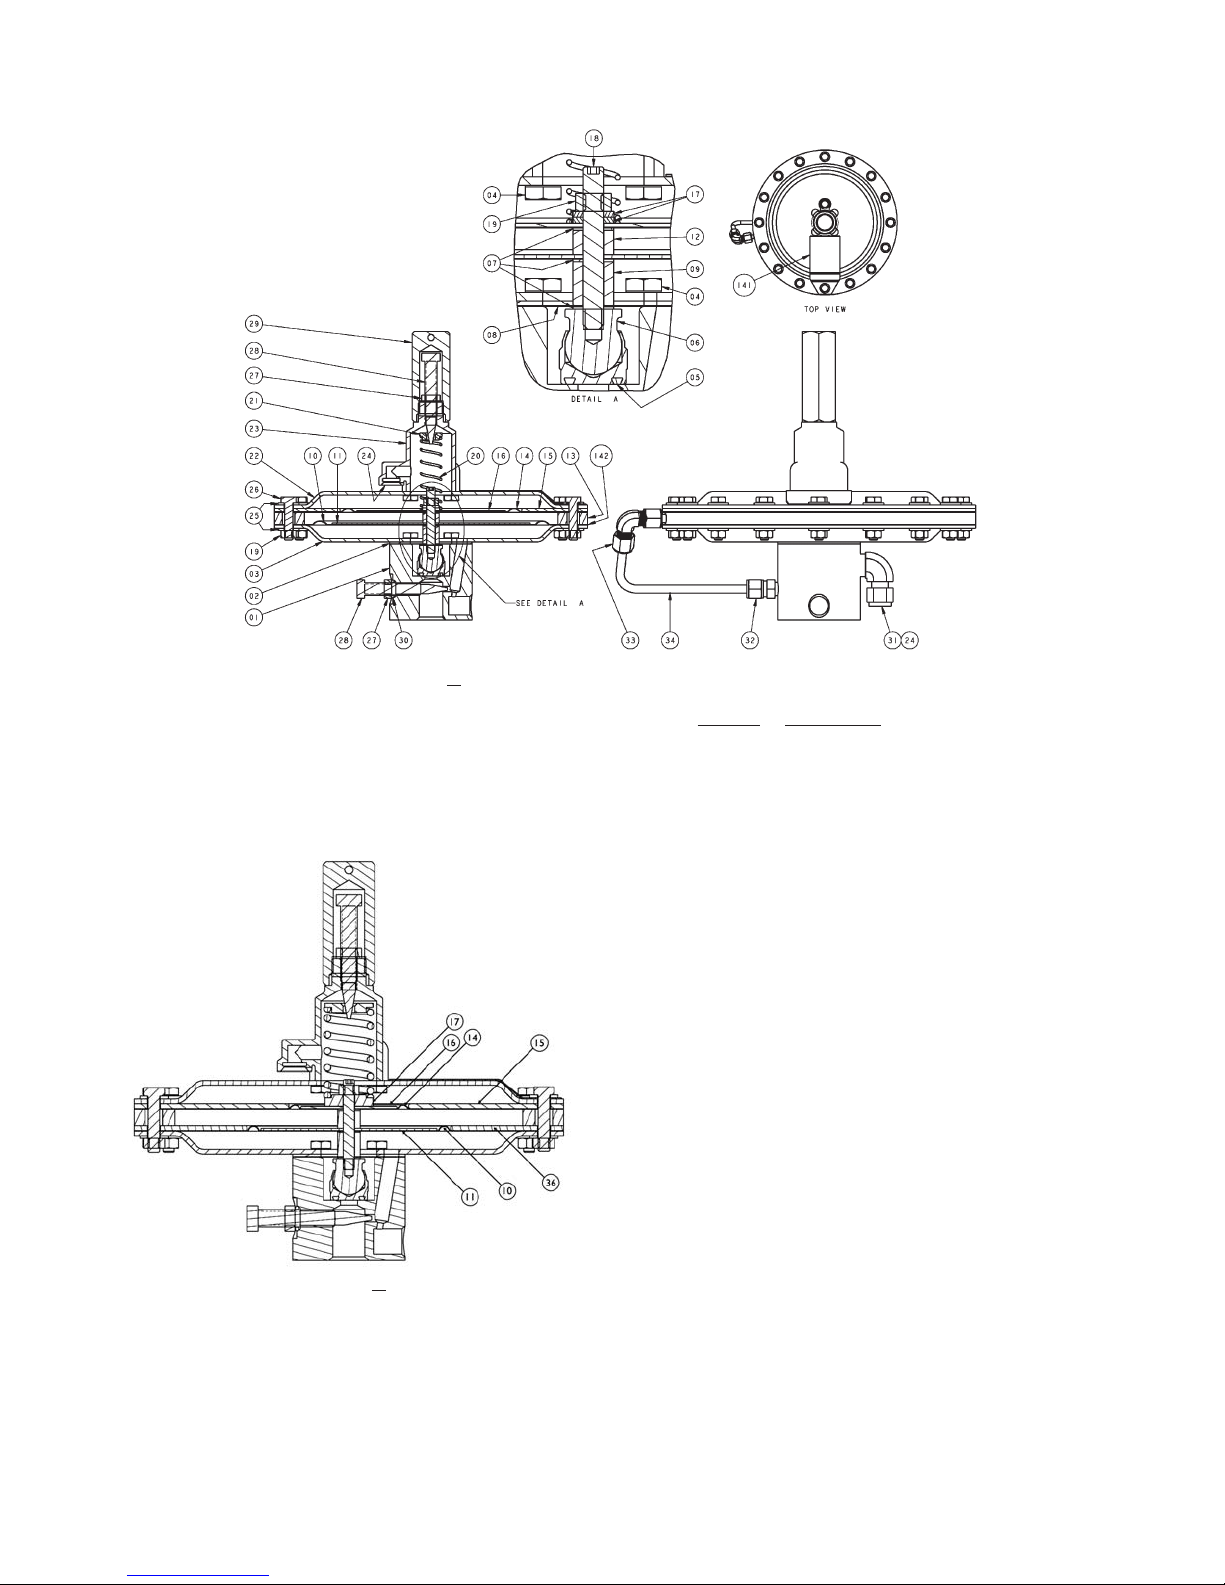
FIGURE 2 - PILOT VALVE
Pilot Pressure < 3.2 psig.
Pilot Pressure > 3.2 psig.
* Spare Parts # Intermediate & High Pressure Pilots ONLY
ITEM NO. DESCRIPTION
01 Body
02 Body Gasket *
03 Lower Diaphragm Case
04 Hex Cap Screw
05 Seat O-Ring *
06 Spindle Assembly
07 Bolt Gasket *
08 Seal Diaphragm *
09 Boost Diaphragm Spacer
10 Boost Diaphragm *
11 Support Plate - Boost
12 Sense Diaphragm Spacer
13 Diaphragm Case Spacer
14 Sense Diaphragm *
15 Sense Pressure Ring
16 Support Plate - Sense
17 Lower Spring Guide
18 Spindle Stud
19 Hex Nut
20 Range Spring
21 Spring Button
22 Upper Diaphragm Case
23 Spring Bonnet
24 Exhaust Screen
25 Flat Washer - Diaphragm Case
26 Hex Cap Screw - Diaphragm Case
27 Jam Nut (Adjusting Screw)
28 Adjusting Screw / Blow down Needle
29 Closing Cap (Spring Bonnet)
30 O-ring (Blowdown Needle) *
31 Exhaust Fitting
32 Straight Tube Fitting
33 Compression Elbow
34 Tubing
36 Boost Pressure Ring #
10
IOM-5400
Page 11
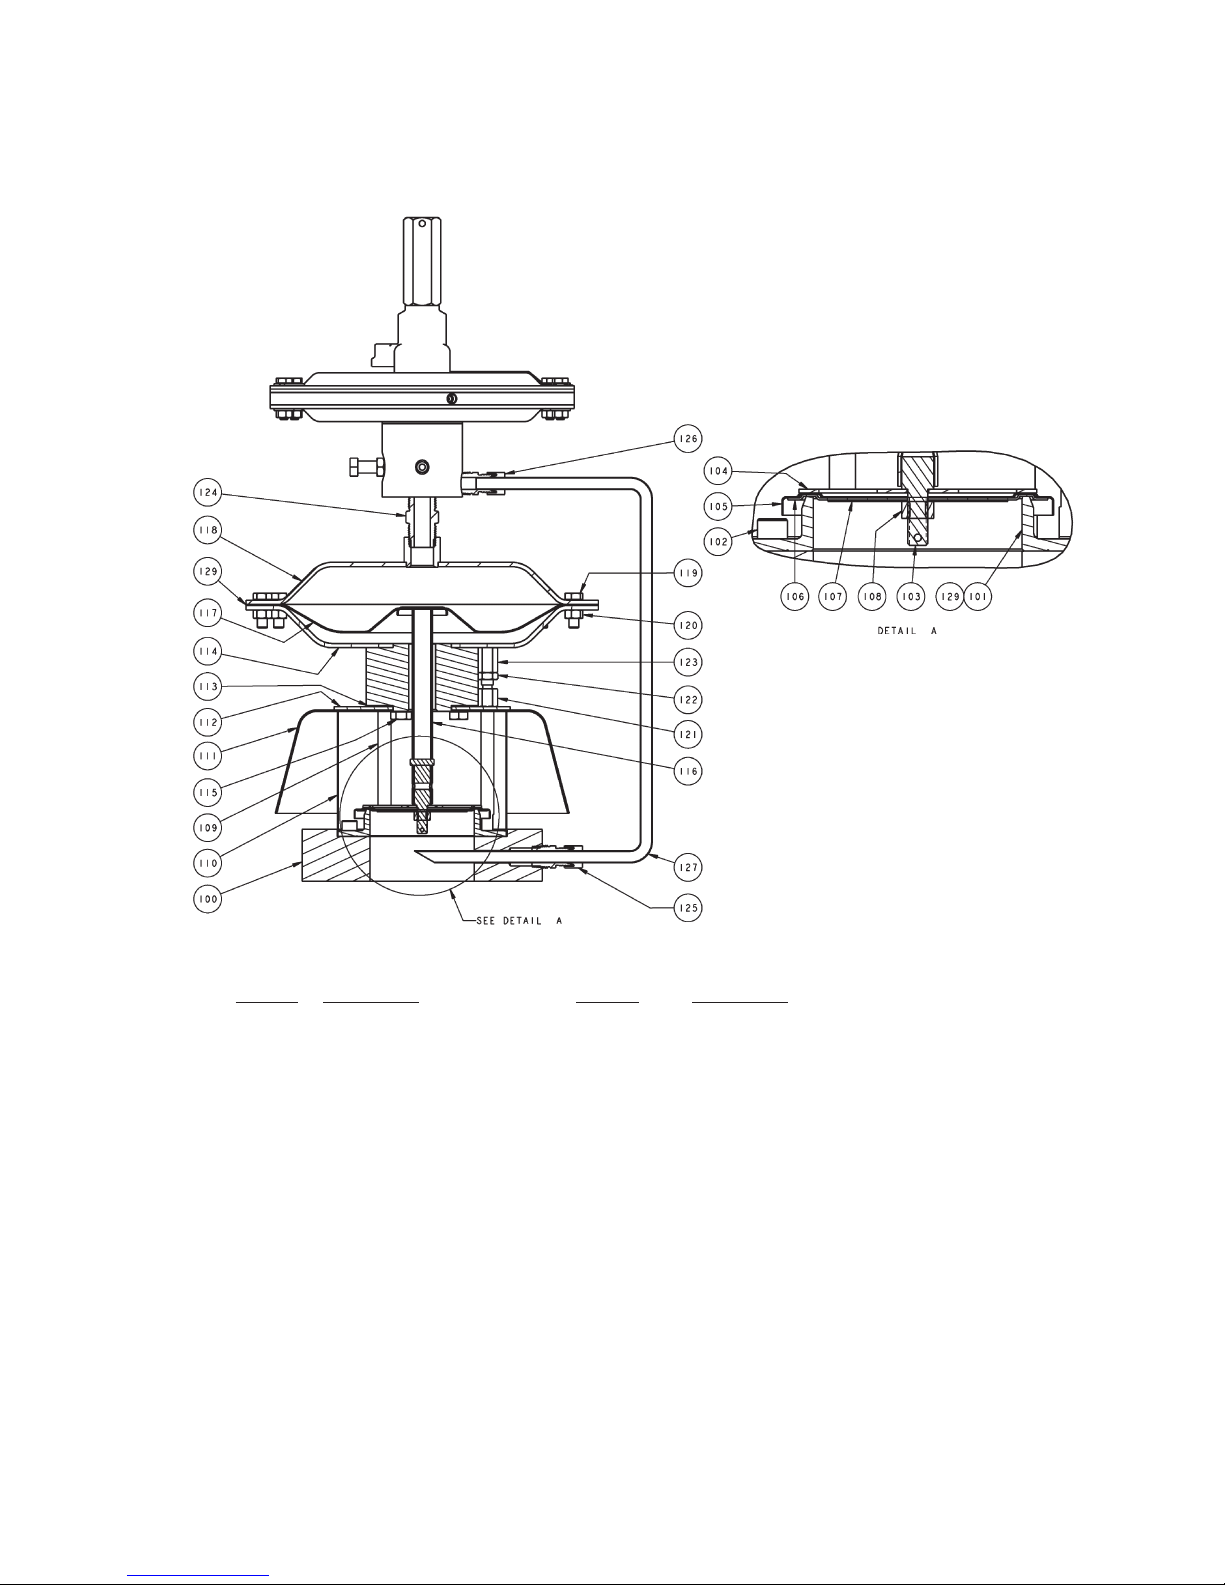
FIGURE 3 - MAIN VALVE
ITEM NO.
100 Body 116 Support Plate
101 Seat Ring 117 Actuator Diaphragm *
102 Seat Ring Bolts 118 Upper Case Assembly
103 Pressure Stem 119 Hex Cap Screw (Actuator Case)
104 Stiffener Plate 120 Hex Nut (Actuator Case)
105 Pressure Pallet 121 Jack Screw
106 Diaphragm * 122 Jam Nut
107 Diaphragm Retainer 123 Jack Nut
108 Lock Nut 124 Pilot Mounting Nipple
109 Pressure Pallet Guide 125 Sense Tube Connector 1
110 Bug Screen 126 Sense Tube Connector 2
111 Weather Hood 127 Sense Tube
112 Weather Hood Plate 128 Name Plate
113 Adapter Gasket * 129 Joint Tape *
114 Lower Case Assembly 130 Lifting Bracket (Not Shown)
115 Hex Cap Screw 130 Hex Cap Screw (Lift Bracket) (Not Shown)
DESCRIPTION ITEM NO. DESCRIPTION
* Spare Parts
IOM-5400
11
Page 12
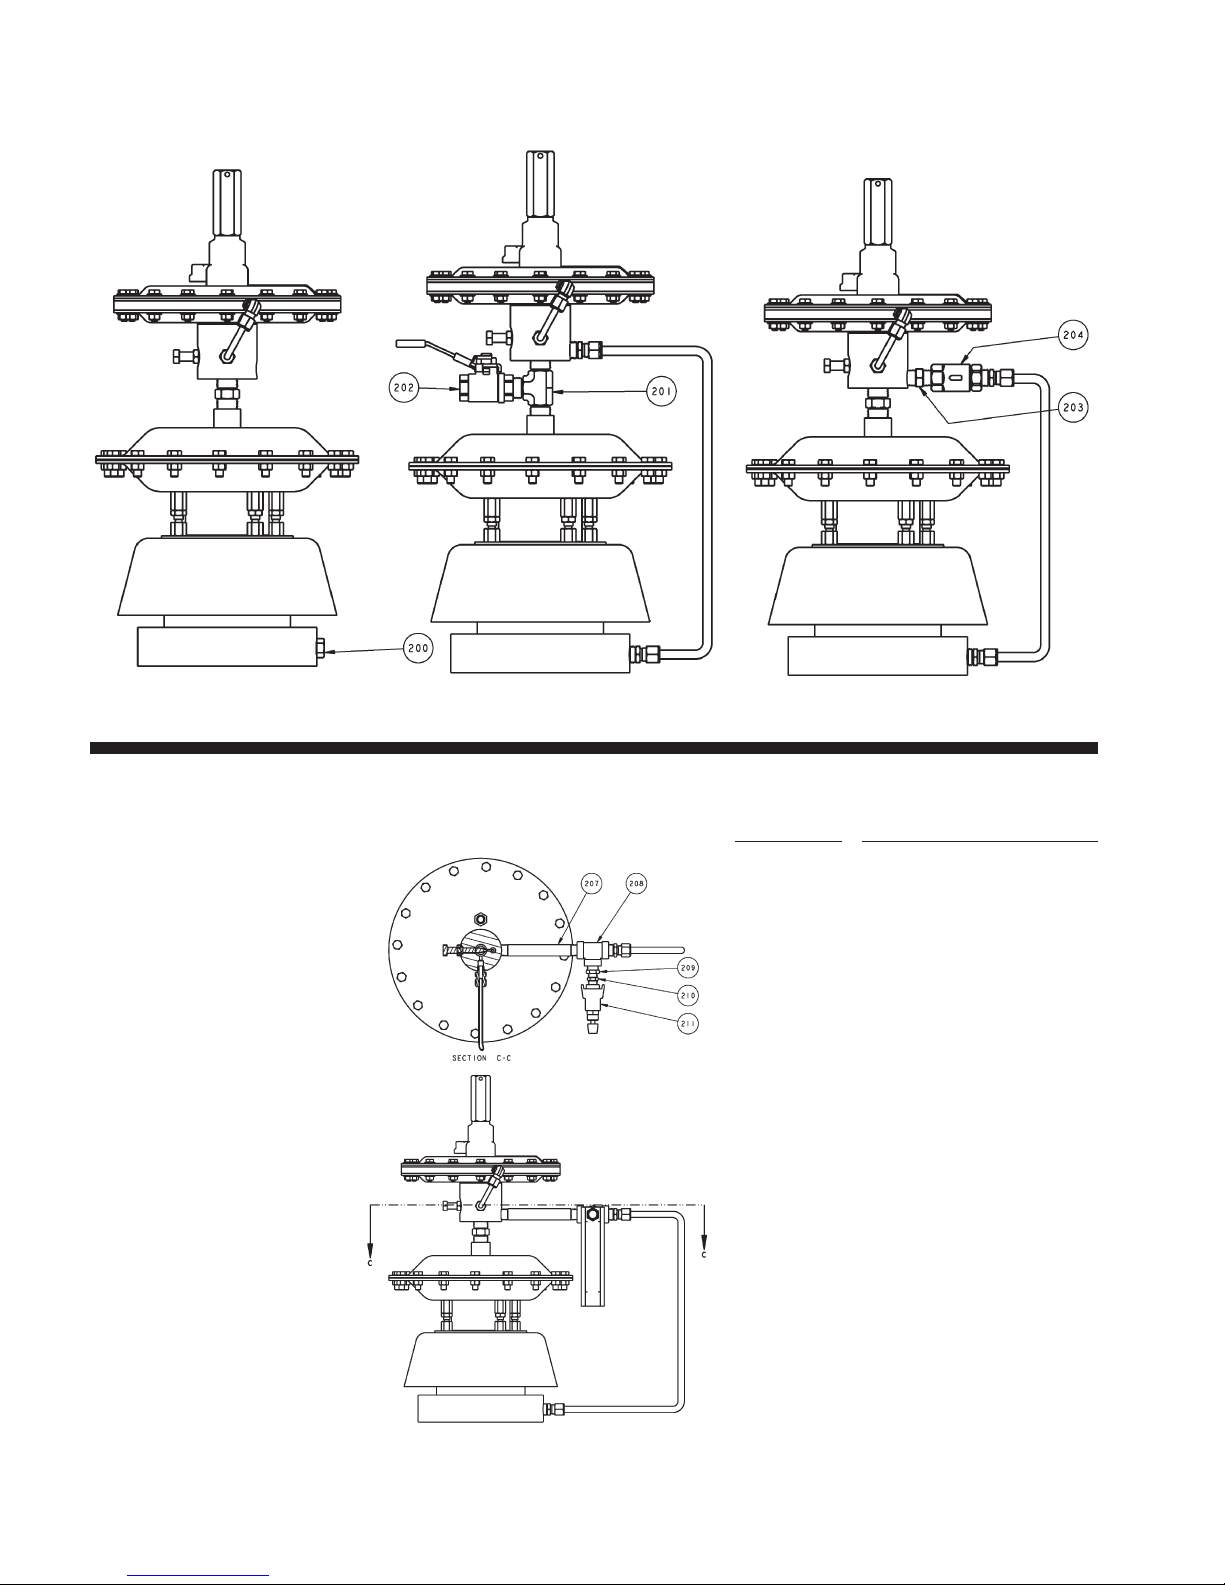
OPTION 1 - Remote Sense OPTION 2 - Manual Blow Down OPTION 3 - Check Valve
SEE ITEM NO. & DESCRIPTION LIST on page 14.
OPTION 4 - Rotometer to Purge Pilot Sense Line
Note: Nipple Length Increases with Line Size.
12
IOM-5400
Page 13
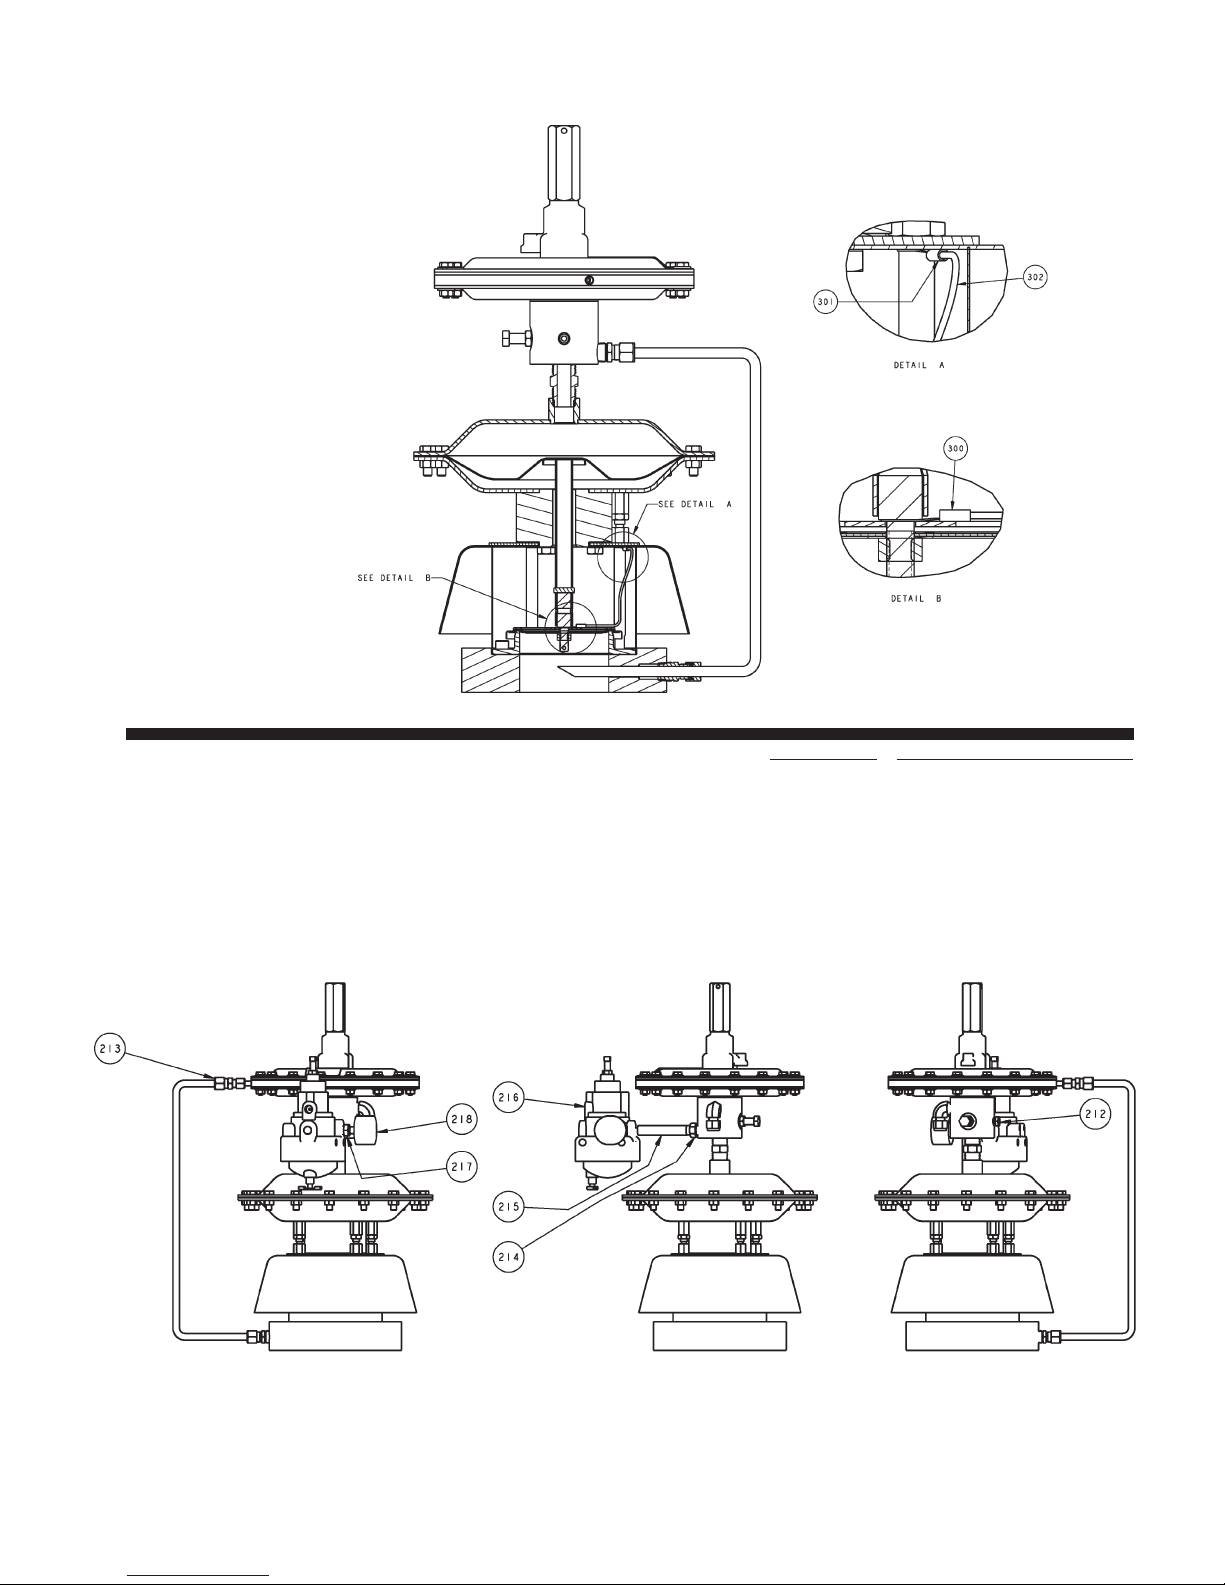
OPTION 5 - Atex
Note: Atex Parts not Applicable for Spring Packs.
OPTION 6 - Air Assist
SEE ITEM NO. & DESCRIPTION LIST on page 14.
IOM-5400
13
Page 14
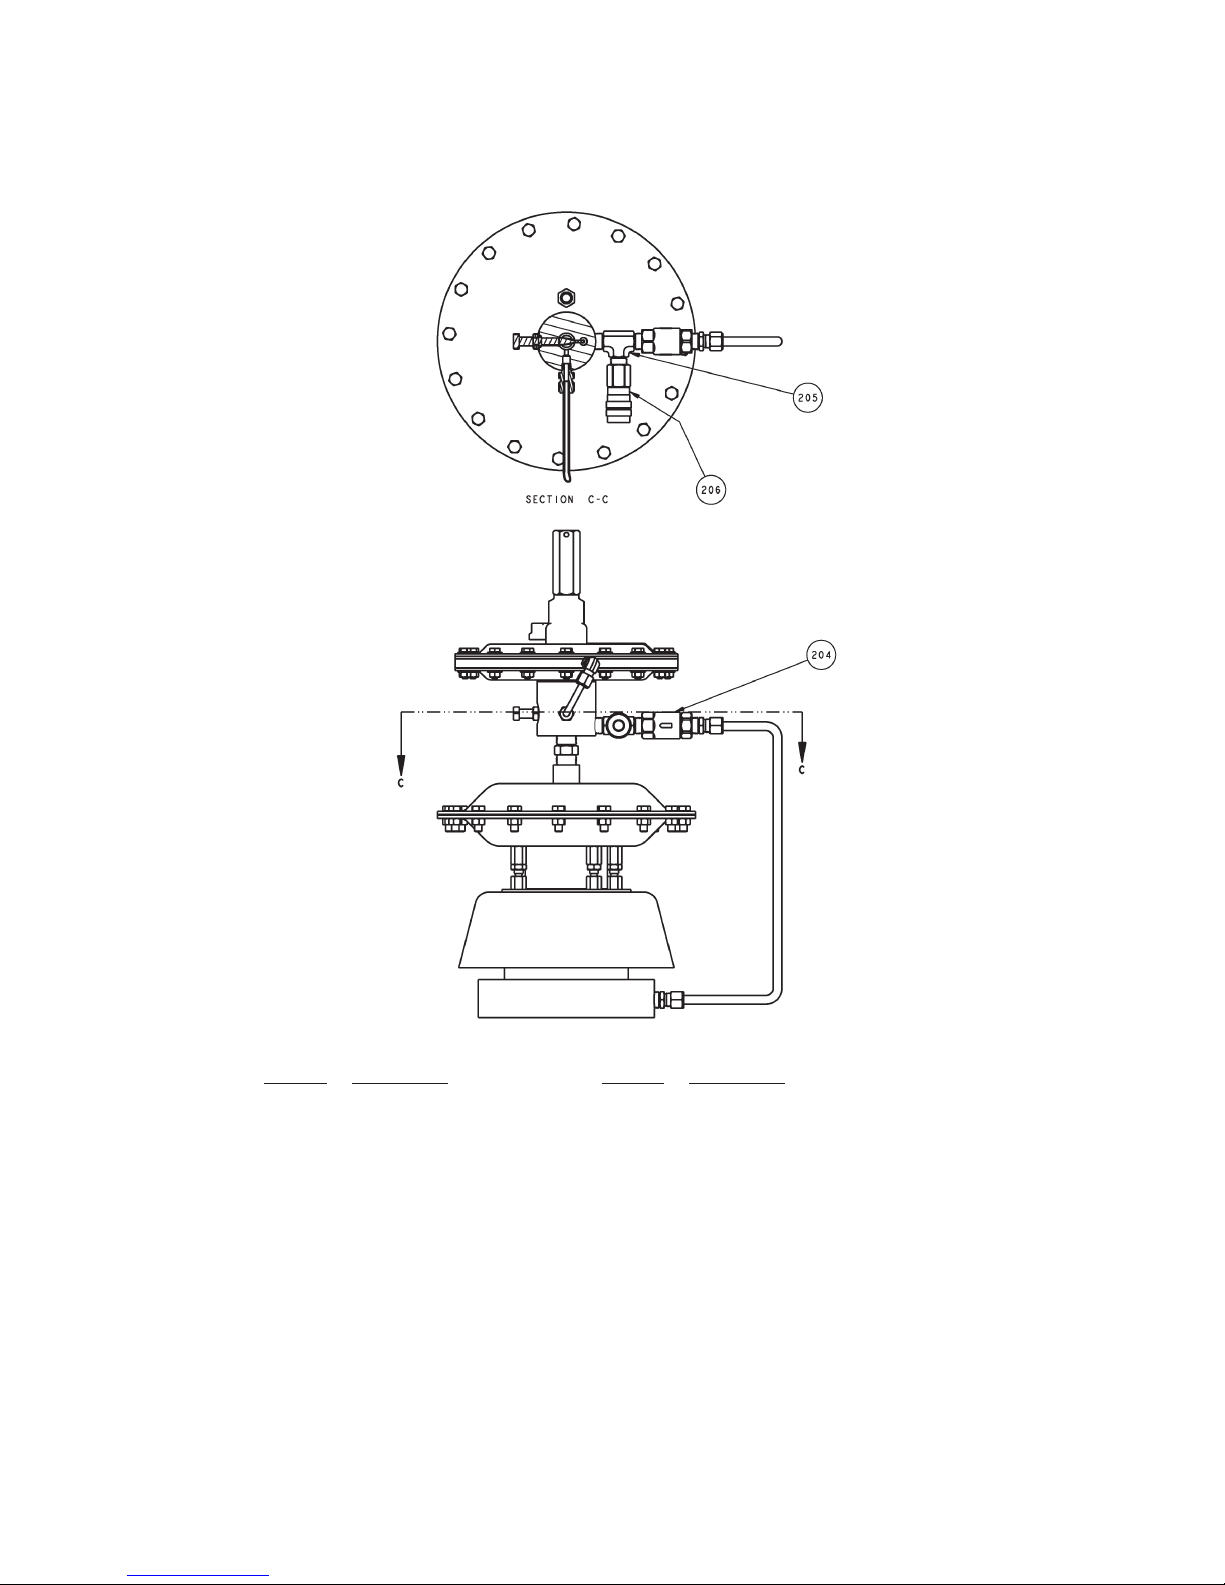
OPTION 7 - Check valve with Field Test Connection
ITEM NO. DESCRIPTION ITEM NO. DESCRIPTION
200 Plug - Remote sense 211 Purge Meter - Purge Opt.
201 MNPT Tee - Manual blowdown 212 Pipe Plug - Air Assist
202 Ball valve - Manual blowdown 213 Sense Tube Connector - FNPT
203 Hex Nipple 214 Red. Bushing - Air Assist
204 Check Valve 215 Nipple - Air Assist
205 MNPT Tee - Field Test Connection 216 Filter / Regulator - Air Assist
206 Push Lock Air Fitting - Field Test 217 Hex Red. Bushing - Gauge - Air Assist
207 Nipple - Purge Option 218 Pressure Gauge - Air Assist
208 Street Tee - Purge Opt. 300 Cable eyelet 1 - ATEX
209 Red. Bushing - Purge Opt. 301 Cable eyelet 2 - ATEX
210 MNPT Flow Orifi ce - Purge Opt. 302 Cable - Pressure - ATEX
14
IOM-5400
Page 15
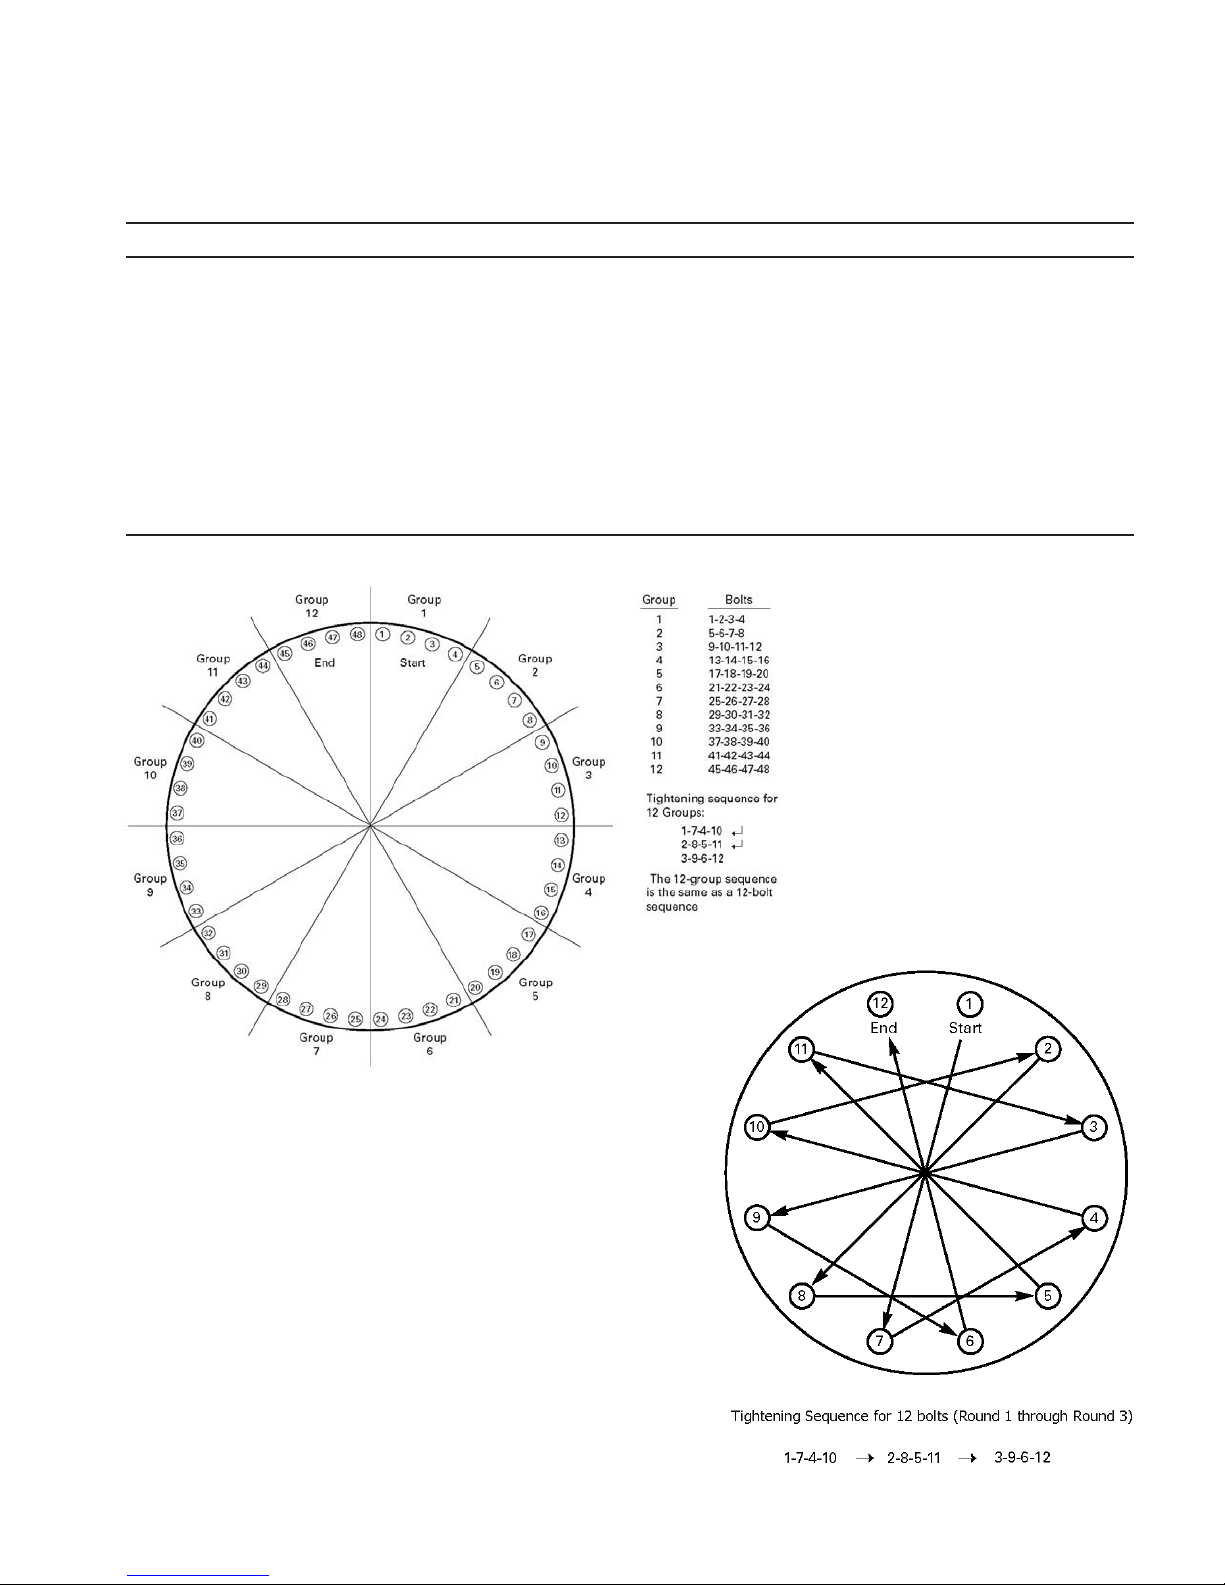
ADDENDUM - A
TIGHTENING SEQUENCE FOR FLANGE BOLTING
GUIDELINES FOR BOLTED FLANGE JOINT ASSEMBLY ACCORDING TO ASME PCC-1 SPECS
STEP LOADING
Install
Hand tighten. Check flange gap around circumference for uniformity. If the gap is not reasonably
uniform, make the appropriate adjustments by selective tightening before proceeding.
Round 1
Round 2
Round 3
Tighten to 20% to 30% of target torque. Check flange gap around circumference for uniformity. If
the gap is not reasonably uniform, make the appropriate adjustments by selective tightening before
proceeding.
Tighten to 50% to 70% of target torque. Check flange gap around circumference for uniformity. If
the gap is not reasonably uniform, make the appropriate adjustments by selective tightening before
proceeding.
Tighten to 100% of target torque. Check flange gap around circumference for uniformity. If the gap
is not reasonably uniform, make the appropriate adjustments by selective tightening.
IOM-5400
15
Page 16
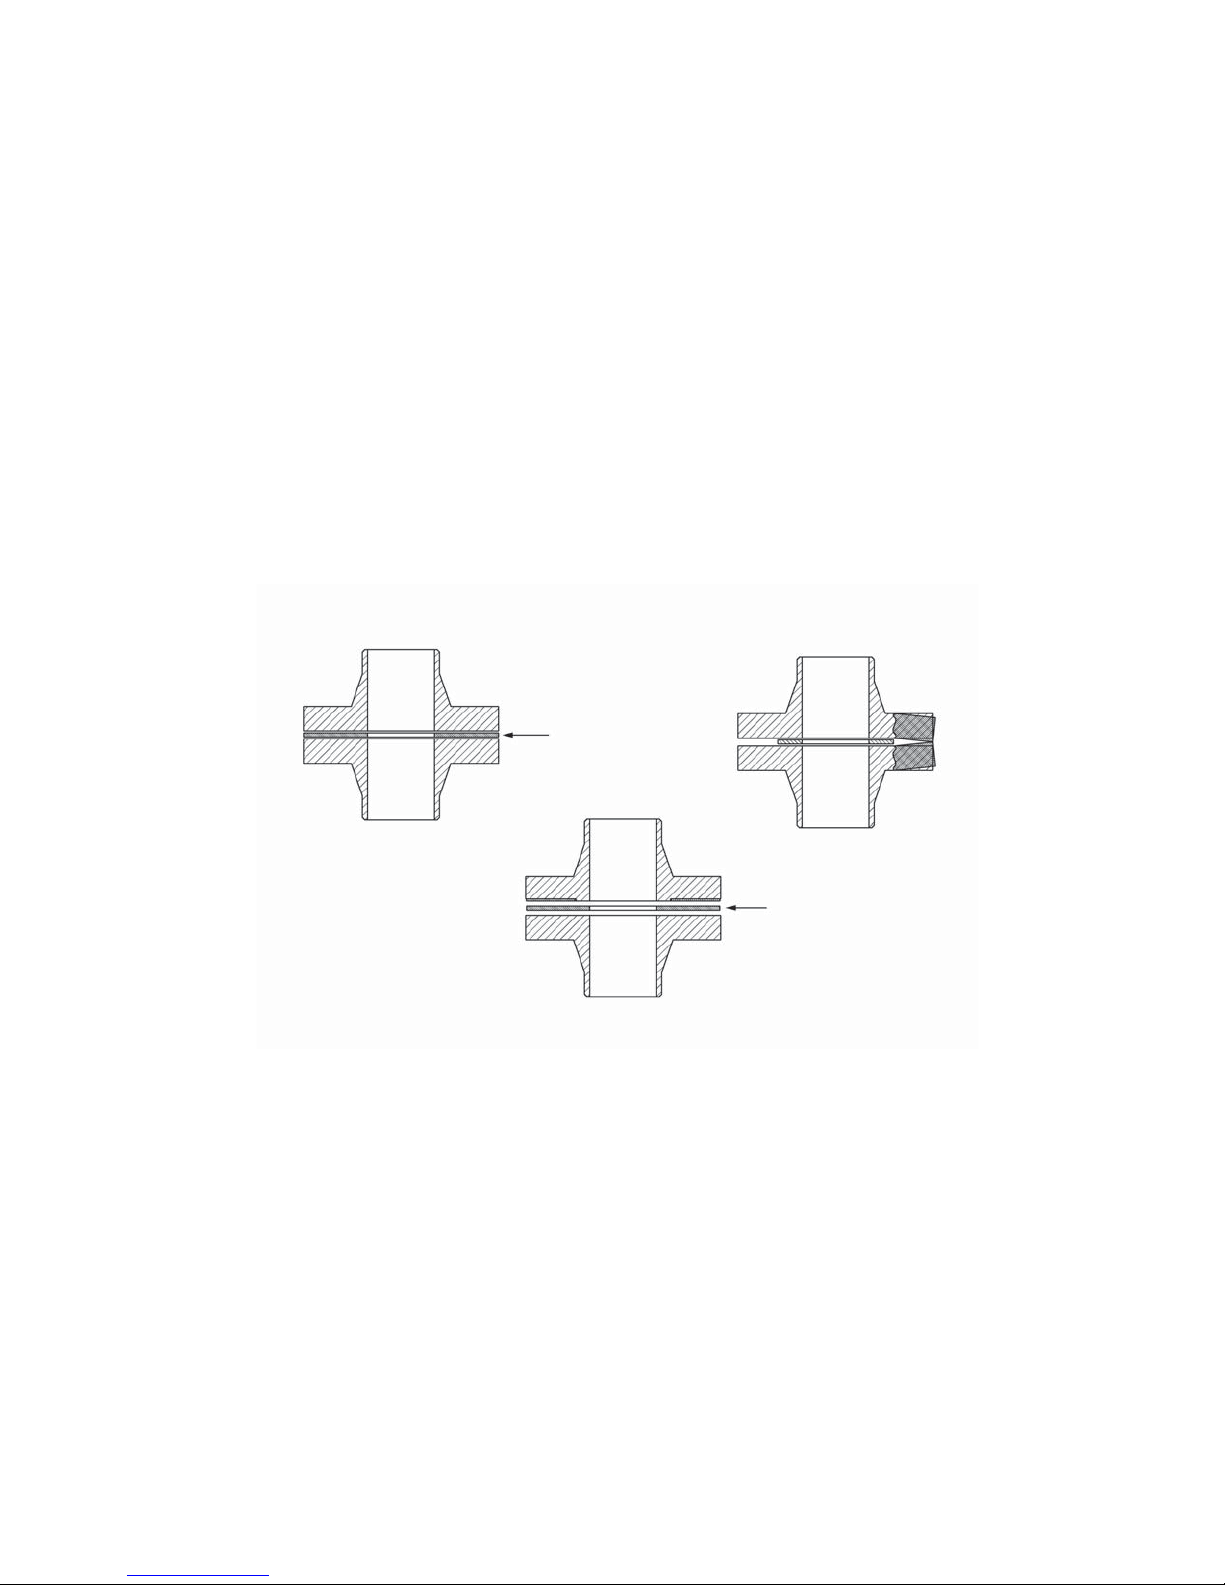
RECOMMENDATIONS FOR PROPER GASKET INSTALLATION
Gasket seating surfaces for tank nozzle flange must be clean, free of scratches,
corrosion, tool marks and flat. Use either a full faced or ring gasket for steel and
stainless steel raised face flanges
FRP and Aluminum vents are furnished with flat faced flanges. It is recommended
that they be installed on mating flat face flanges with a full faced gasket. If the flat
face of the vent is sealing against a raised face steel flange, a spacer or filler ring
must be used to fill the annular space of the raised face steel flange.
Refer to Gasket Dimension Table.
Ensure that the gasket material is suitable for the service.
gasket is compressed evenly and the flanges are not distorted. Utilizing proper
torquing techniques will ensure a tight seal and prevent leakage around the
gasket. See preceding page.
NOTE: Incorrect positioning and/or selection of gasket(s) between the flanges
will cause bending stresses at the flange that may damage the flange joint
as bolting is tightened. This is more likely to occur with aluminum or cast iron
materials.
Make sure that the
Correct Installation
Incorrect Installation
Full Faced Gasket
Spacer and
Full Faced Gasket
Correct Installation
Cashco, Inc.
P.O. Box 6
Ellsworth, KS 67439-0006
PH (785) 472-4461
Fax. # (785) 472-3539
www.cashco.com
email: [email protected]
Printed in U.S.A. 5400-IOM
Cashco GmbH
Handwerkerstrasse 15
15366 Hoppegarten, Germany
PH +49 3342 30968 0
Fax. No. +49 3342 30968 29
www.cashco.com
email: [email protected]
Cashco do Brasil, Ltda.
Al.Venus, 340
Indaiatuba - Sao Paulo, Brazil
PH +55 11 99677 7177
Fax. No.
www.cashco.com
email: [email protected]
 Loading...