

Page 1
A
Operator Instructions Important
T
Includes - Foreseen Use, Work Stations, Putting Into Service,
Operating, Dismantling, Assembly and Safety Rules
Manufacturer/Supplier Product Type
Universal Air Tool Company Limited
Unit 8
Lane End Industrial Park
High Wycombe
Bucks
HP14 3BY
Tel No Fax No
(01494) 883300 (01494) 883237
Read these instructions carefully before insta lling, operating,
servicing or repairing this tool. Keep these instructions in a safe
accessible place.
Die Grinder - Right
ngle Head
Model No/Nos Serial No
UT5715
RPM
22,000
Cycles Per Min
Product Nett Weight
1.10
0.50 3/8 10 30 10
Recommended Working
Recommended Minimum
Maximum
lbs
Kg
Air Pressure
Personal Safety Equipment
Use - Safety Glasses
Use - Safety Gloves
Use - Safety Boots
Use - Breathing Masks
Use - Ea r P ro t ec to r s
Foreseen Use Of The Tool
This die grinder is prima rily de signe d for u se with bonded
abrasive mounted point grinding wheels. It may also be used
with ste el rotary files and carbide bu rrs provided their speed
rating matches the speed of the grinder.
This tool should not be fitted with cutting off wheels, saw
blades, drill bits, etc. If there is any doubt about the correct use
of this product contact your supplier for advice.
Also make sure th at the shank s ize of the a ttachment to be
driven matches with the collet size fitted in the grinder and that
the maximum allowed running spee d of the attachment exceeds
that marked on the grinder.
There are special rules governing the use of bonded abrasive
mounted point grinding wheels - for details see section
"Operating".
Recommended Use Of
Balancer Or Support
No
6.3
bar
90
PSI
n/a
bar
n/a
PSI
7
bar
100
Yes
Yes
Yes
Yes
PSI
Recommended Hose Bore
Size - Minimum
Ins M/M Ft M
Noise Level
Sound Pressure Level 90.0 dB(A)
Sound Power Level 97.0 dB(A)
Test Method
Tested in accordance with Pneurop
test code PN8NTC1 and ISO Standard 3744
Vibration Level
Test Method
Less than 2.5
ested in accordance with ISO
standard 8662 Parts 1 & 17
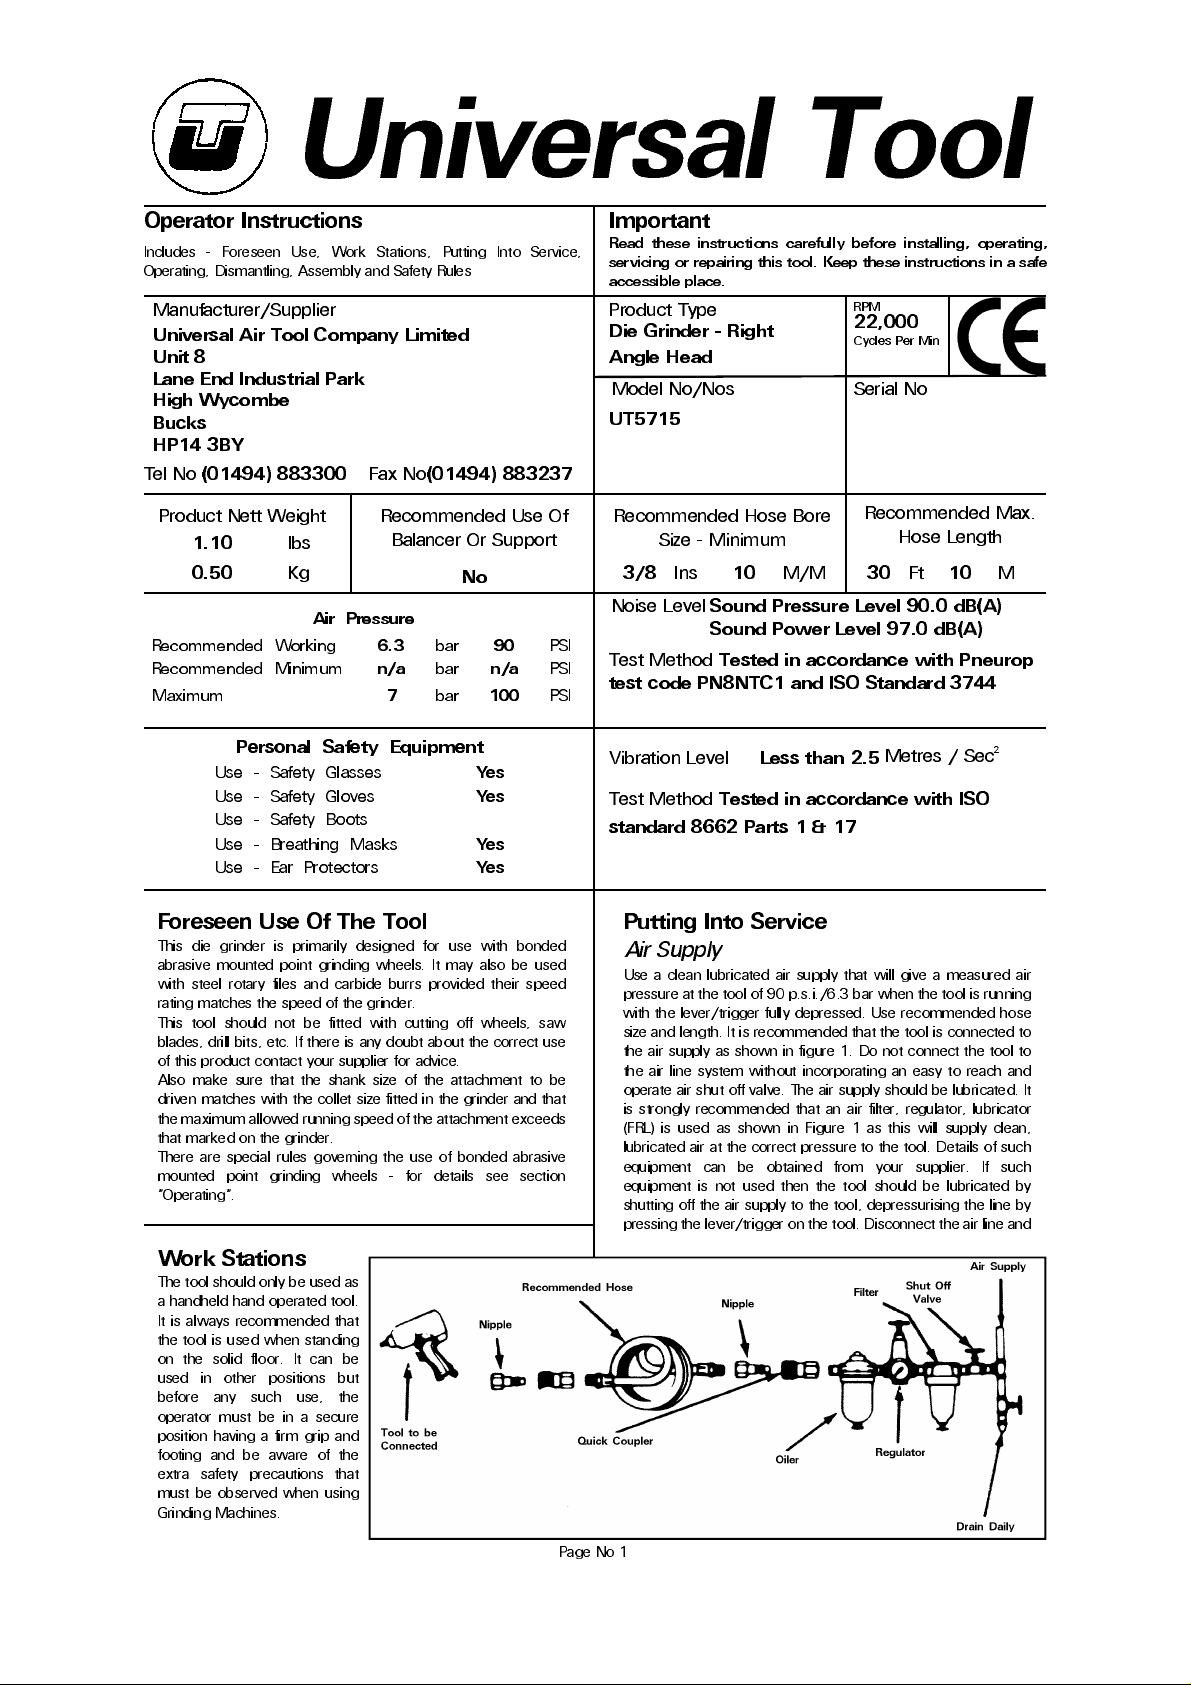
Putting Into Service
Air Supply
Use a clean lubricated air supply that will give a measured air
pressure at the tool of 90 p.s.i./6.3 bar when the tool is running
with the lever/trigger fully depressed. Use recommended hose
size and length. It is recommended that the tool is connected to
the air supply as shown in figure 1. Do not connect the tool to
the air line system without incorporating an easy to reach and
operate air shut off valve. The air supply should be lubricated. It
is strongly recommended that an air filter, regulator, lubricator
(FRL) is used as shown in Figure 1 as this will supply clean ,
lubricated air at the correct pressure to the tool. Details of such
equipment can be obtained from your supplier. If such
equipment is not used then the tool should be lubricated by
shutting off the air supply to the tool, depressurising the line by
pressing the lever/trigger on the tool. Disconnect the air line and
Recommended Max.
Hose Length
Metres / Sec²
Work Stations
The tool should only be used as
a handheld hand operated tool.
It is always recommended that
the tool is used when standing
on the solid floor. It can be
used in other positions but
before any such use, the
operator mus t be in a secur e
position having a firm grip and
footing and be aware of the
extra safety precautions that
must be observed when using
Grinding Machines.
Page No 1
Page 2
pour into the intake bushing a teaspoonful (5ml) of a suitable
k
pneumatic motor lubricating oil preferably incorporating a rust
inhibitor. Reconnect tool to air supply and run tool slowly for a
few sec onds to allow air to circulate the oil. If tool is used
frequently lubricate on daily basis and if tool starts to slow or
lose power.
It is recommended that the air pressure at the tool whilst the
tool is running is 90 p.s.i./6.3 bar. The tool can run at lower and
higher pressures with the maximum permitted working air
pressure of 100 p.s.i./7.0 bar.
If tool is used daily then every other day grease gears (27) &
(32) via grease plug (40).
Operating
Select a suitable mounted point that has a free running speed
higher than the maximum running speed marked on the tool.
Make sure that the diameter of the shank exactly matches the
diameter of the collet mounted in the grinder. There are three
standard sizes of collet available for use with this grinder, i.e.
1) - 1/4" Dia (0.250ins) (6.35mm)
2) - 6mm (0.236ins)
3) - 1/8" (0.125ins) (3.175mm)
Never try to force a 1/4" diameter shank into a 6mm collet.
Never try to close a 1/4" diameter collet to secure a 6mm
shank. Always match correctly the shank size to the collet size.
If uncertain, have parts measured by
a competent person.
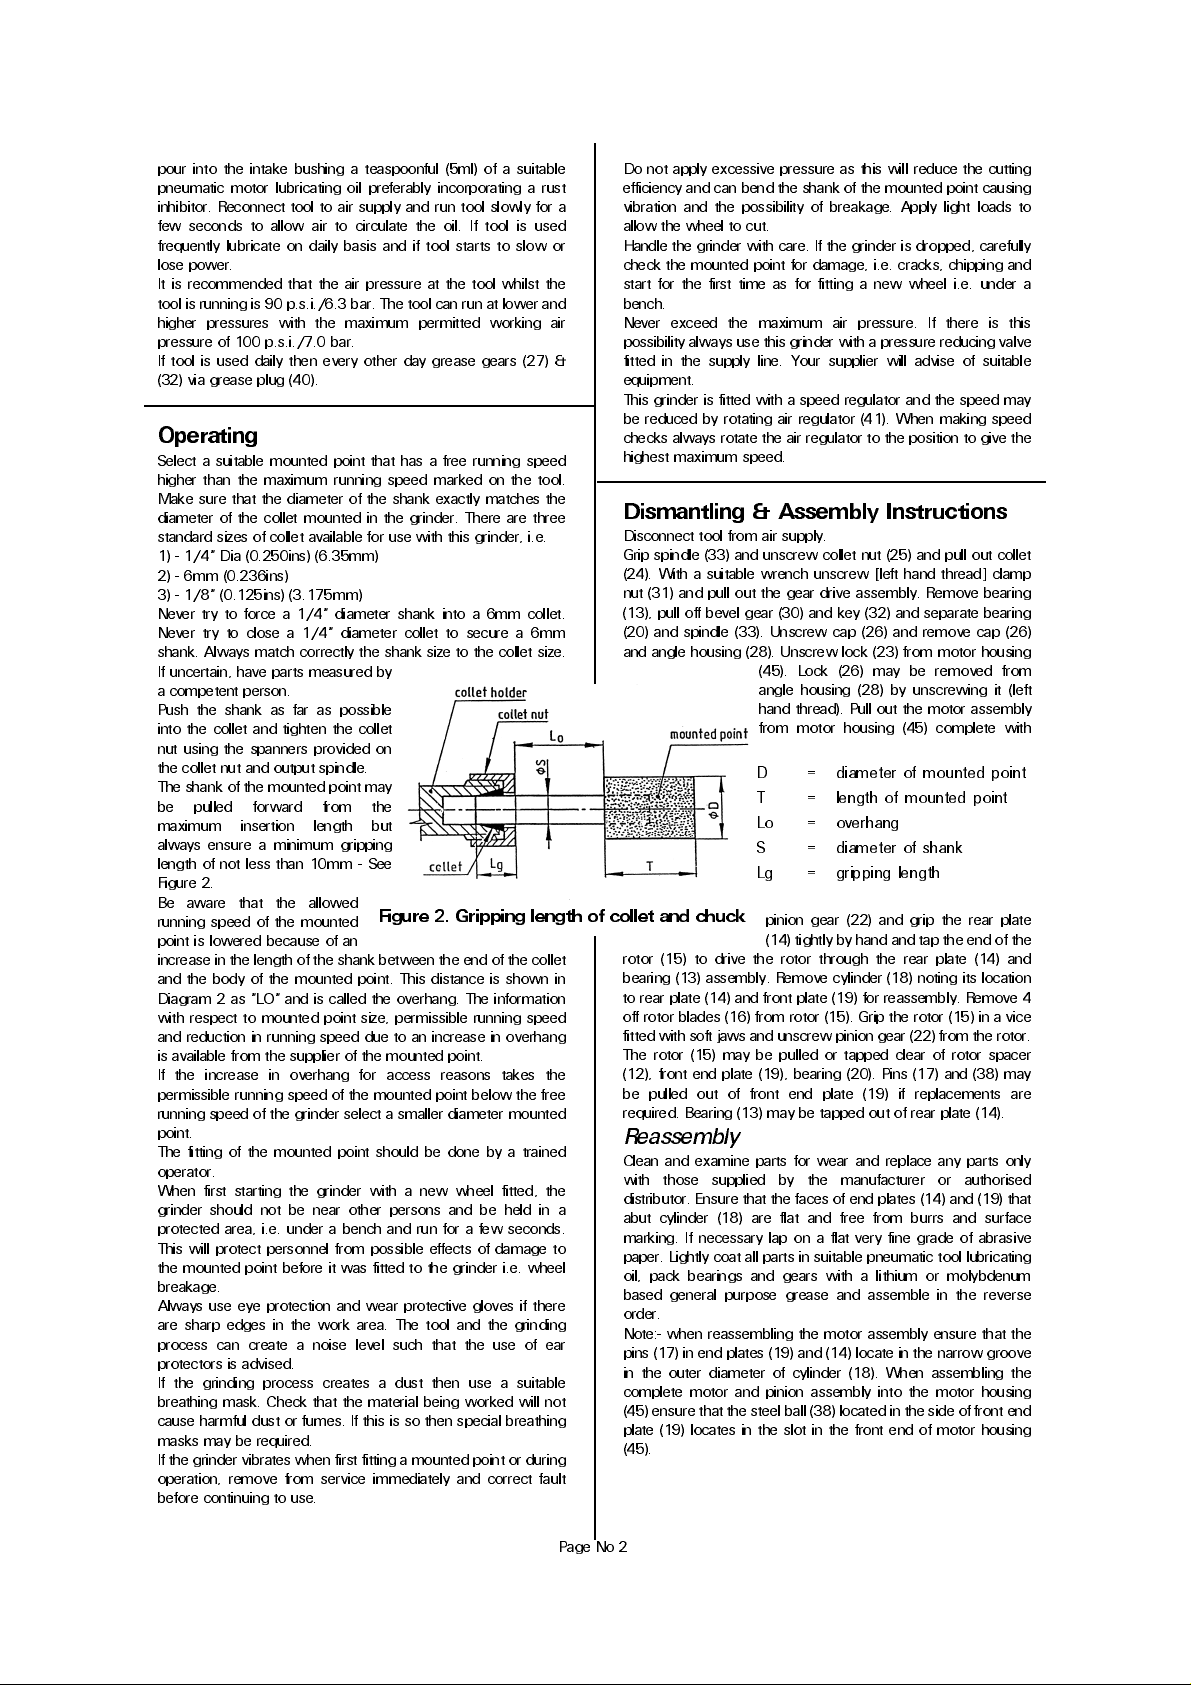
Push the shank as far as possible
into the collet and tighten the collet
nut using the spanners provided on
the collet nut and output spindle.
The shank of the mounted point may
be pulled forward from the
maximum insertion length but
always ensure a minimu m gripping
length of not less than 10mm - See
Figure 2.
Be aware that the allowed
running speed of the mounted
point is lowered because of an
increase in the length of the shank between the end of the collet
and the body of the mounted point. This distance is shown in
Diagram 2 as "LO" and is called the overhang. The information
with respect to mounted point size, permissible running speed
and reduction in running speed due to an increase in overhang
is available from the supplier of the mounted point.
If the increase in overhang for access reasons takes the
permissible running speed of the mounted point below the free
running speed of the grinder select a smaller diameter mounted
point.
The fitting of the mounted point should be done by a trained
operator.
When first starting th e grinder w ith a ne w whee l fitted, the
grinder should not be near othe r persons and be held in a
protected area, i.e. under a bench and run for a few seconds.
This will protect personnel from possible effects of damage to
the mounted point before it was fitted to the grinder i.e. wheel
breakage.
Always use eye protection and wear protective gloves if there
are sharp edges in the work area. The tool and the grinding
process can create a noise level such that the use of ear
protectors is advised.
If the grinding process creates a dust then use a suitable
breathing mask. Check that the material being worked will not
cause harmful dust or fumes. If this is so then special breathing
masks may be required.
If the grinder vibrates when first fitting a mounted point or during
operation, re move from service immediately and corre ct fault
before continuing to use.
Figure 2. Gripping length of collet and chuc
Do not apply excessive pressure as this will reduce the cutting
efficiency and can bend the shank of the mounted point causing
vibration an d the possibility of breakage. Apply light loads to
allow the wheel to cut.
Handle the grinder with care. If the grinder is dropped, carefully
check the mounted point for damage, i.e. cracks, chipping and
start for the first time a s for fitting a new wheel i.e. un der a
bench.
Never exceed the maximum air pressure. If there is this
possibility always use this grinder with a pressure reducing valve
fitted in the s upply line. Your supplier will advise of suitable
equipment.
This grinder is fitted with a speed regulator and the speed may
be reduced by rotating air regulator (41). When making speed
checks always rotate the air regulator to the position to give the
highest maximum speed.
Dismantling & Assembly Instructions
Disconnect tool from air supply.
Grip spindle (33) and unscrew collet nut (25) and pull out collet
(24). With a suitable wrench unscrew [left hand thread] clamp
nut (31) and pull out the gear drive assembly. Remove bearing
(13), pull off bevel gear (30) and key (32) and separate bearing
(20) and spindle (33). Unscrew cap (26) and remove cap (26)
and angle housing (28). Unscrew lock (23) from motor housing
(45). Lock (26) may be removed from
angle housing (28) by unscrewing it (left
hand thread). Pull out the motor assembly
from motor hous ing (45) complete with
D = diameter of mounted point
T = length of mounted point
Lo = overha n g
S = diameter of shank
Lg = gripping lengt h
pinion gear (22) and grip the rear plate
(14) tightly by hand and tap the end of the
rotor (15) to drive the rotor through the rear plate (14) and
bearing (13) assembly. Remove cylinder (18) noting its location
to rear plate (14) and front plate (19) for reassembly. Remove 4
off rotor blades (16) from rotor (15). Grip the rotor (15) in a vice
fitted with soft jaws and unscrew pinion gear (22) from the rotor.
The rotor (15) may be pulled or tapped clear of rotor spacer
(12), front end plate (19), bearing (20). Pins (17) and (38) may
be pulled out of front end plate (19) if replacements are
required. Bearing (13) may be tapped out of rear plate (14).
Reassembly
Clean and examine parts for wear and replace any parts only
with those supplied by the manufacturer or authorised
distributor. Ensure that the faces of end plates (14) and (19) that
abut cylinder (18) are flat and free from burrs and surface
marking. If necessary lap on a flat very fine grade of abrasive
paper. Lightly coat all parts in suitable pneumatic tool lubricating
oil, pack bearings and gears with a lithium or molybdenum
based gen eral purpose gre ase an d assemble in the re verse
order.
Note:- when reassembling the motor assembly ensure that the
pins (17) in end plates (19) and (14) locate in the narrow groove
in the outer diameter of cylinder (18). When assembling the
complete m otor and pinion assembly into the motor housing
(45) ensure that the steel ball (38) located in the side of front end
plate (19) locates in the slot in the front end of motor housing
(45).
Page No 2
Page 3
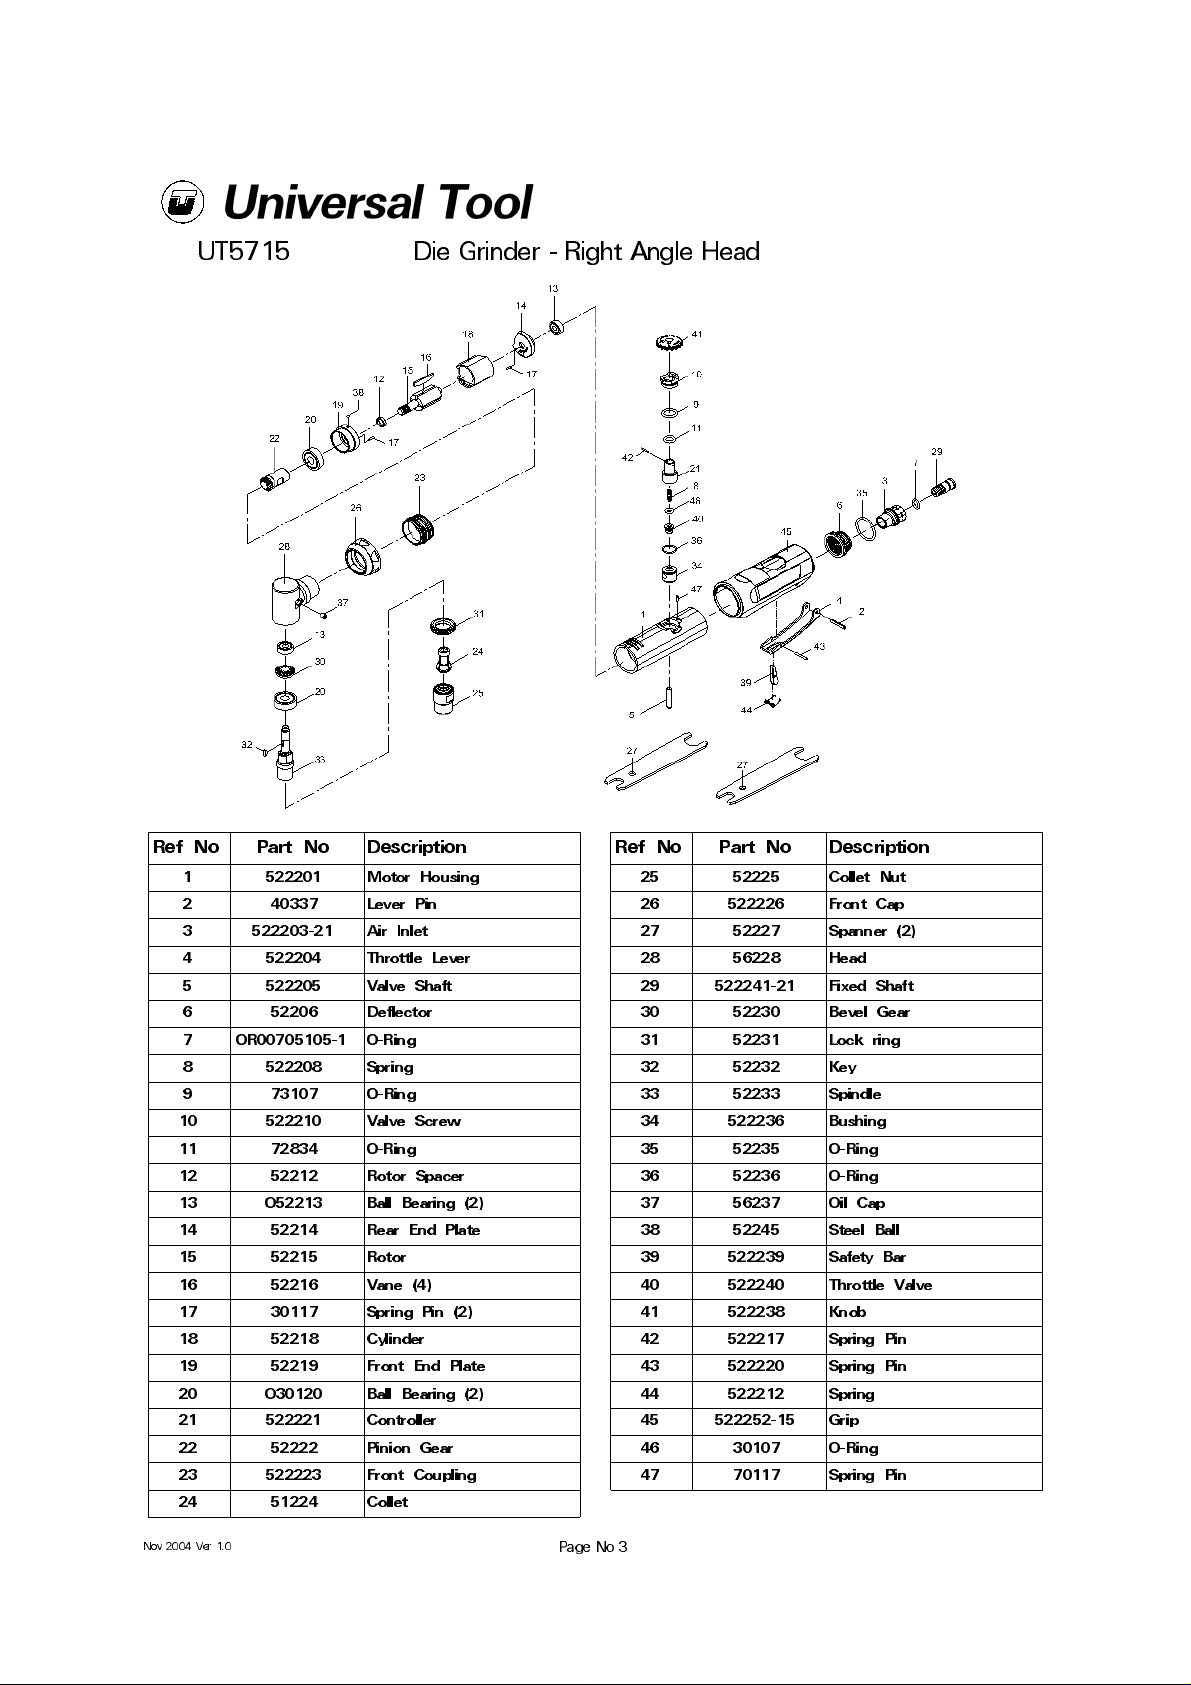
UT5715 Die Grinder - Right Angle Head
Ref No Part No Description
1 52220 1 Motor Housi ng
2 40337 Lever Pi n
3 52220 3-21 Air In let
4 52220 4 Throttle Lev er
5 52220 5 Valve Sh af t
6 52206 Deflector
7 OR00705105-1 O-Ring
8 522208 Spring
9 73107 O-Ring
10 522210 Valve Screw
11 72834 O-Ring
12 52212 Rotor Spacer
13 O5221 3 Ball Bear ing (2)
14 52214 Rear End Plate
15 52215 Rotor
16 52216 Vane (4)
17 30117 Spring Pin (2)
18 52218 Cylinder
19 52219 Front End Plate
20 O3012 0 Ball Bear ing (2)
21 522221 Controller
22 52222 Pinion Gear
23 522223 Front Coupling
24 51224 Collet
Ref No Part No Description
25 52225 Collet Nut
26 522226 Front Cap
27 5 22 27 Spanner (2)
28 56228 Head
29 522241-21 Fixed Shaft
30 52230 Bevel Gear
31 52231 Lock ring
32 52232 Key
33 52233 Spindle
34 522236 Bushing
35 52235 O-Ring
36 52236 O-Ring
37 56237 Oil Cap
38 52245 Steel Ball
39 522239 Safety Bar
40 522240 Throttle Valve
41 522238 Knob
42 522217 Spring Pin
43 522220 Spring Pin
44 522212 Spring
45 522252-15 Grip
46 30107 O-Ring
47 70117 Spring Pin
Nov 2004 Ver 1.0
Page No 3
Page 4
Declaration of Conformity
Universal Air Tool Company Limited
Unit 8, Lane End Industrial Park, High Wycombe, Bucks, HP14 3BY, England
declare under our sole responsibility that the product
Model UT5715 Die Grinder (R/A Head), Serial Number
to which this declaration relates is in conformity with the following standard(s) or other normative document(s)
EN792 (Draft), EN292 Parts 1 & 2, ISO 8662 Parts 1 & 17, Pneurop PN8NTC1
following the provisions of
89/392/EEC as amended by 91/368/EEC & 93/44/EEC Directives
Lane End
Place and date of issue Name and signature or equivalent marking of authorised person
D.H.Moppett (Man. Director)
Safety Rules When Using A Die Grinder
1) Read all the instructions before using this tool. All operators
must be fully trained in its use and aware of these safety rules.
2) Always select suitable abrasive to use with this tool - see
Operating Instructions.
3) Always shut off the air supply to the grinder and depress the
lever to exhaust air from the feed hose before fitting, adjusting
or removing the mounted point.
4) Always adopt a firm footing and/or position before using the
grinder.
5) Use only correct spare parts.
6) Check hose and fittings regularly for wear. Do not carry the
tool by its hose.
7) Do not remove and never tie down the safety lever.
8) Never exceed the maximum air pressure and check the free
running speed frequently. Have air regulator fully open.
9) Use safety equipment as recommended.
10) Take care against entanglement of moving parts of the tool
with clothing, ties, hair, cleaning rags, etc.
11) Use only compressed air at the recommended pressure.
12) Do not attempt to fit any other attachment than those
recommended - see “Foreseen Use of Tool”
13) If the tool appears to malfunction remove from use
immediately and arrange for service and repair.
Notes
Accessories
Distributor
This document may not be copied wholly or in part by anyone without the consent of the Directors of Universal Air Tool Company Limited
Designed & Written in the U.K.
©Copyright of Universal Air Tool Company Limited, established in the United Kingdom, 1994
Page No 4
 Loading...