

Page 1
Page 1 of 7
L E A D E R S IN M A RINE COMP O SITE
F I T TINGS
Web: www.trudesignplastics.com REV D
PRODUCT
INFORMATION
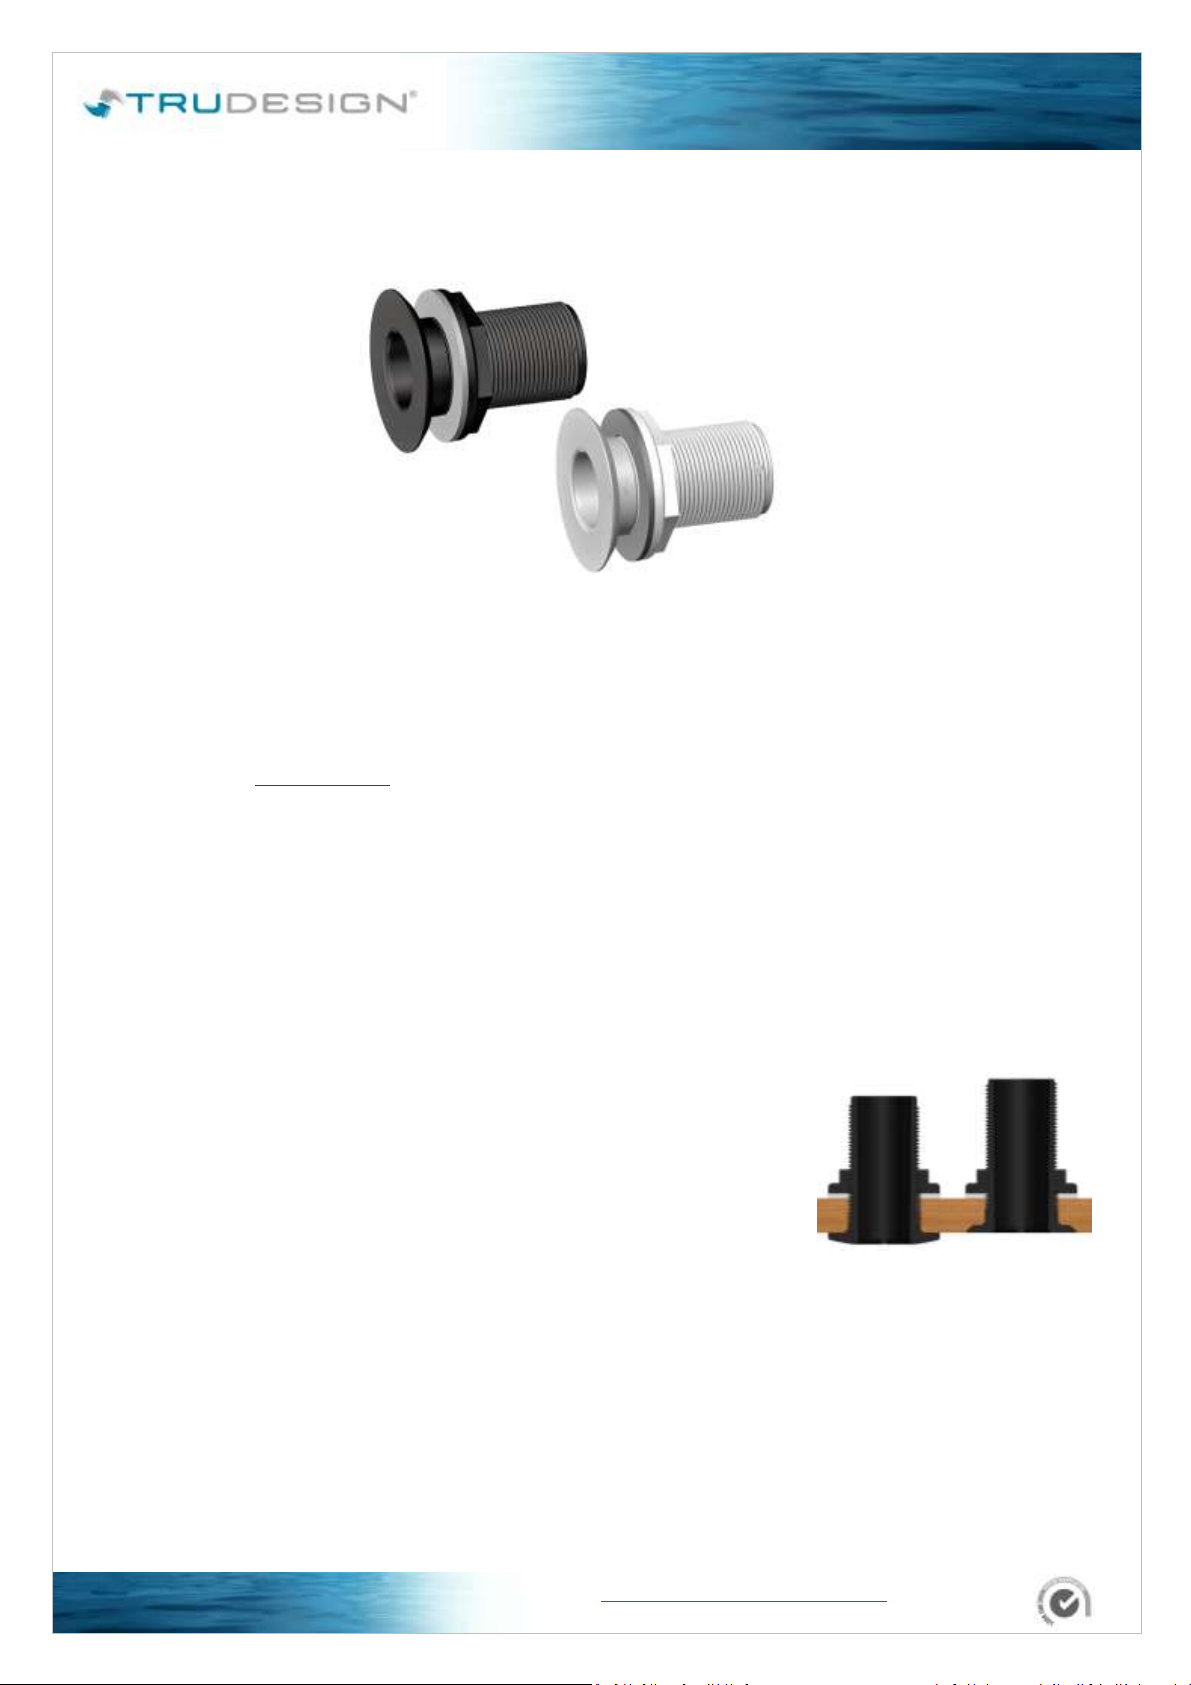
Recessed Skin Fittings (Thru Hulls)
Designed and made in New Zealand, TruDesign Skin Fittings (Thru Hulls) are precision moulded from glass-reinforced
Nylon composite.
• Certified to ISO 9093-2 by the International Marine Certification Institute (IMCI, Belgium).
• Comply with ABYC H-27 standards when used in conjunction with the TruDesign ABYC collar.
• Certified by Bureau Veritas to ISO 9093-2.
TruDesign Skin Fittings (Thru Hulls) eliminate all corrosion and bonding problems associated with electrolysis giving
peace of mind with respect to the safety of your vessel.
Features:
▪ Low profile for less drag below the water line.
▪ Compatible with all hull types – Can be used on aluminium, steel, wood,
composite & GRP hulls.
▪ Immune to corrosion & electrolysis – No corrosion breakages, increased
safety.
▪ Chemical resistant – Unaffected by diesel, petrol, chemicals, and
antifouling paints.
▪ U.V resistant – Will not degrade or discolour from the sun’s ultraviolet
rays.
▪ Paintable – Paintable with all types of antifoul including Coppercoat™
▪ Fits TruDesign Ball Valves and other parallel BSP or NPS threads –
Universal compatibility to TRUDESIGN™ brand fittings and other marine
hardware.
▪ Large operating range – Suitable for all marine conditions from -40°C to
+110°C
▪ Meet ABYC H-27 Standard when installed in combination with TruDesign
Ball Valves & Load Bearing Collars.
Page 2
Page 2 of 7
L E A D E R S I N M A R IN E C O MP OS I T E
F I TT IN GS
Web: www.trudesignplastics.com REV D
PRODUCT
INFORMATION
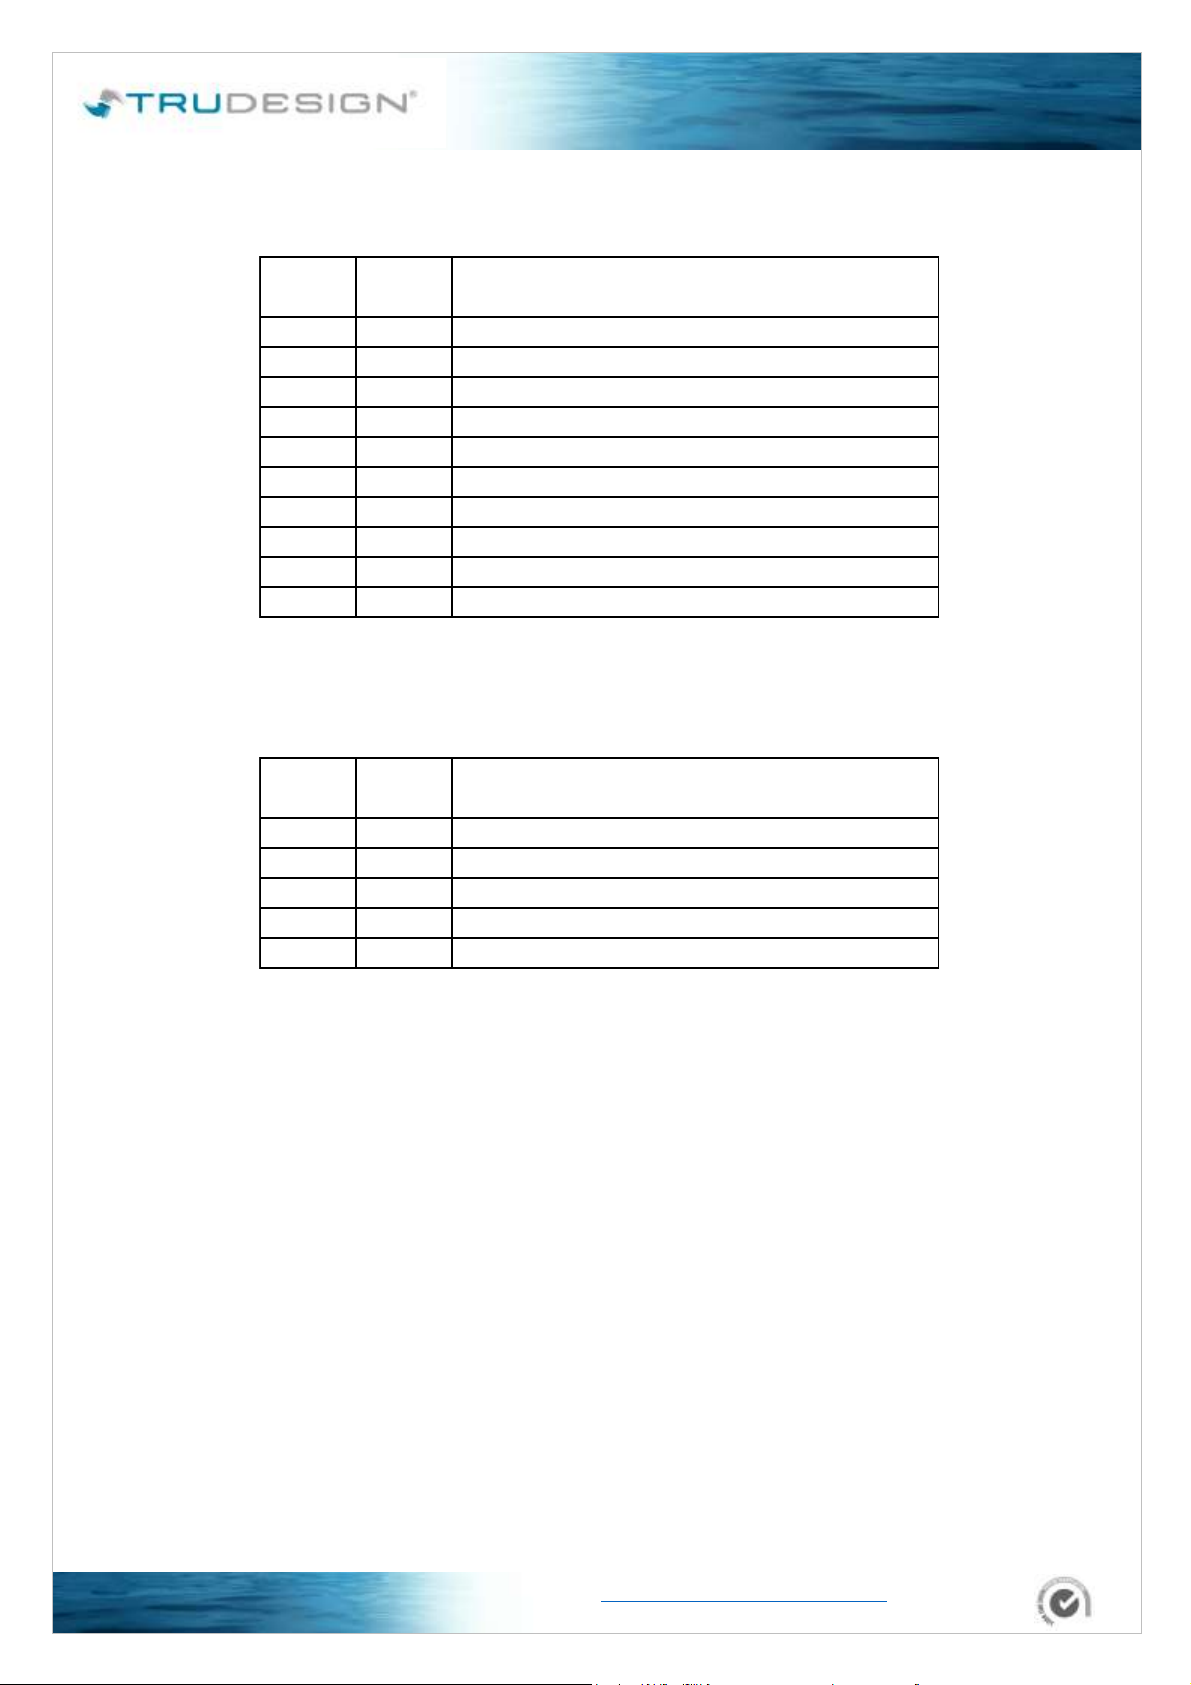
Part Numbers BSP
Part #
Black
Part #
White
SKIN FITTINGS / THRU HULLS - RECESSED
90676 90709
Skin Fitting Recessed ½” BSP PKG
91125 91131
Skin Fitting Recessed ½” BSP Tagged
90677 90710
Skin Fitting Recessed ¾” BSP PKG
91126 91132
Skin Fitting Recessed ¾” BSP Tagged
90678 90711
Skin Fitting Recessed 1” BSP PKG
91127 91133
Skin Fitting Recessed 1” BSP Tagged
90679 90712
Skin Fitting Recessed 1¼” BSP PKG
91128 91134
Skin Fitting Recessed 1¼” BSP Tagged
90680 90713
Skin Fitting Recessed 1½” BSP PKG
91129 91135
Skin Fitting Recessed 1½” BSP Tagged
Part Numbers NPS
Part #
Black
Part #
White
SKIN FITTINGS / THRU HULLS - RECESSED
91237 91242
Thru-hull Recessed ½" NPS
91238 91243
Thru-hull Recessed ¾" NPS
91239 91244
Thru-hull Recessed 1" NPS
91240 91245
Thru-hull Recessed 1¼" NPS
91241 91246
Thru-hull Recessed 1½" NPS
Page 3
Page 3 of 7
L E A D E R S I N M A R IN E C O MP OS I T E
F I TT IN GS
Web: www.trudesignplastics.com REV D
PRODUCT
INFORMATION
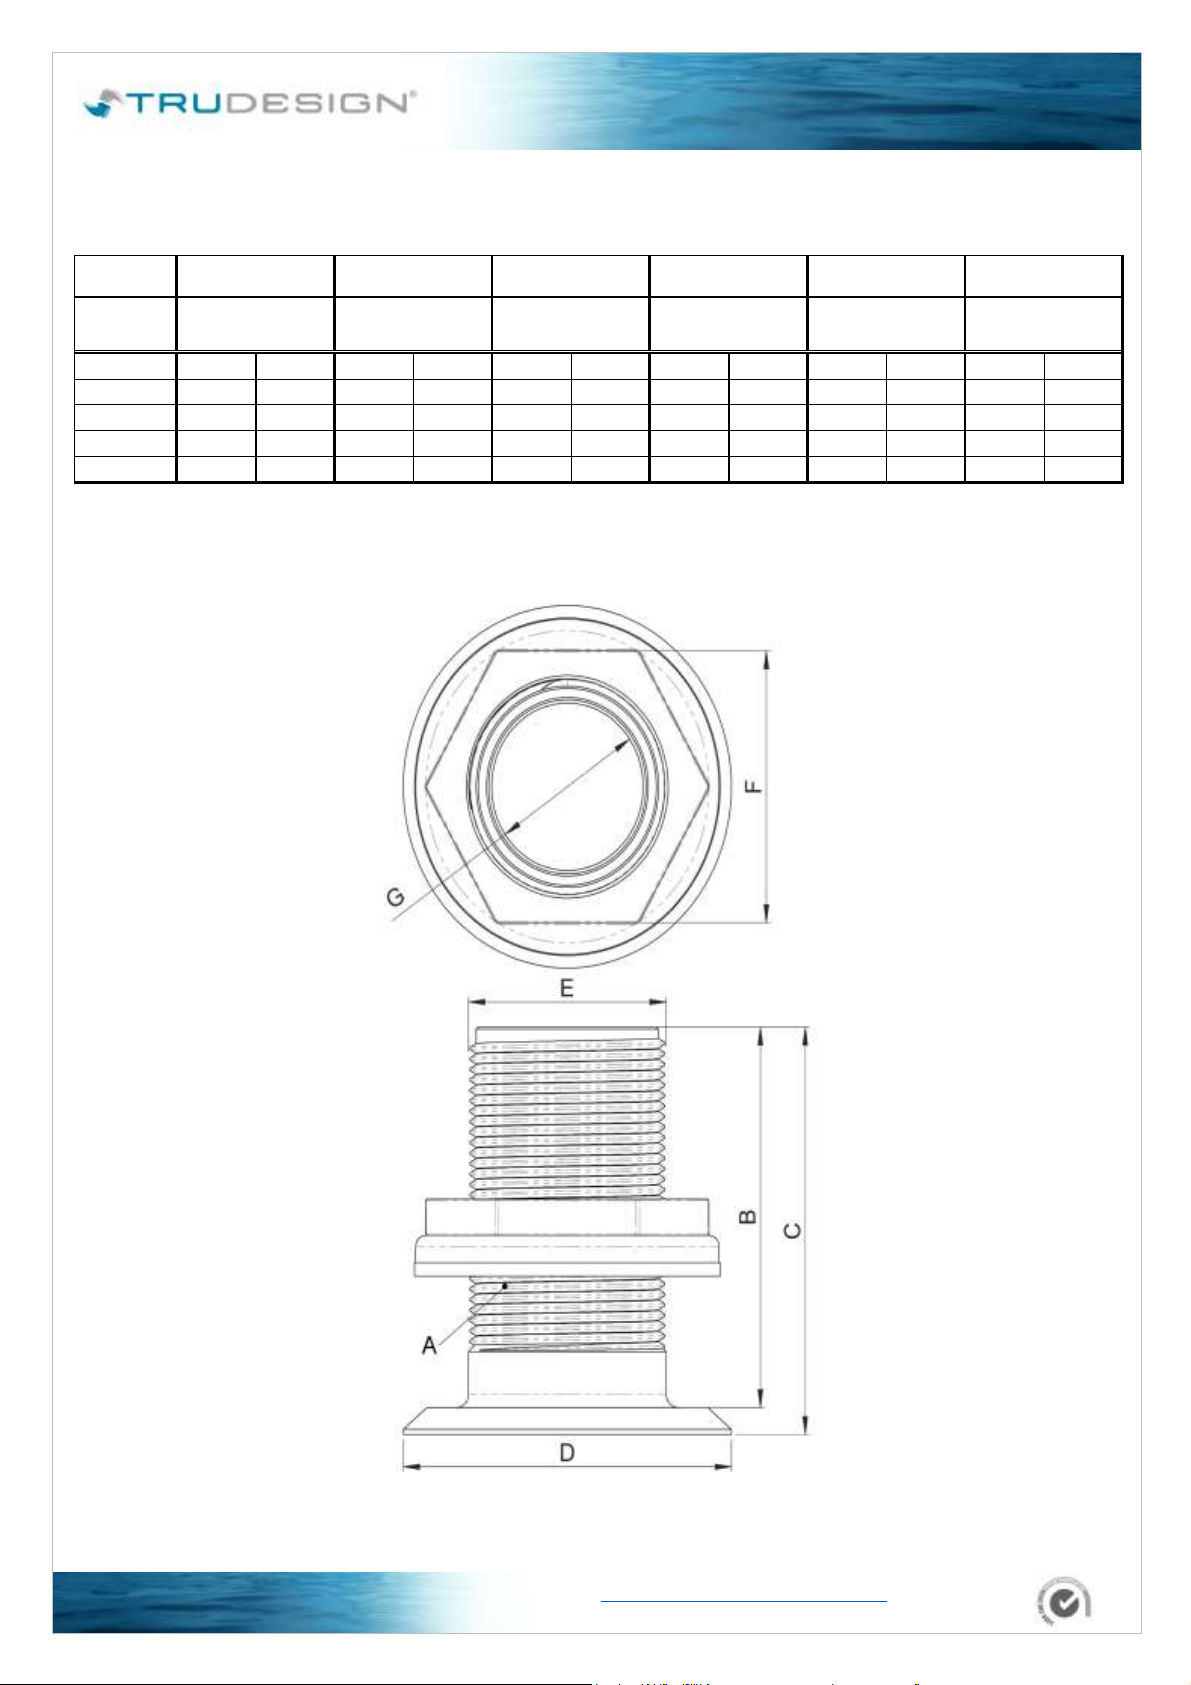
Dimensions
A
Thread
Size
½" 67mm 2 2/3'' 70mm 2 3/4'' 32mm 1 1/4'' 22mm 6/7'' 28mm 1 1/9'' 12mm 1/2''
¾" 66mm 2 4/7'' 70mm 2 3/4'' 42mm 1 2/3'' 27mm 1" 34mm 1 1/3'' 17mm 2/3''
1" 66mm 2 4/7'' 70mm 2 3/4'' 52mm 2" 34mm 1 1/3'' 42mm 1 2/3'' 23mm 1"
1¼" 85mm 3 1/3'' 90mm 3 1/2'' 64mm 2 1/2'' 42mm 1 2/3'' 52mm 2" 30mm 1 1/5''
1½" 84mm 3 1/3'' 90mm 3 1/2'' 80mm 3 1/7'' 48mm 1 8/9'' 60mm 2 1/3'' 36mm 1 2/5''
Thread Length
Head Diameter
Cutout Diameter
Hex Size AF
Minimum Internal
Ø
Overall Length
GBDEF
C
Dimensions All dimensions in millimetres. All dimensions nominal.
Page 4
Page 4 of 7
L E A D E R S I N M A R IN E C O MP OS I T E
F I TT IN GS
Web: www.trudesignplastics.com REV D
PRODUCT
INFORMATION
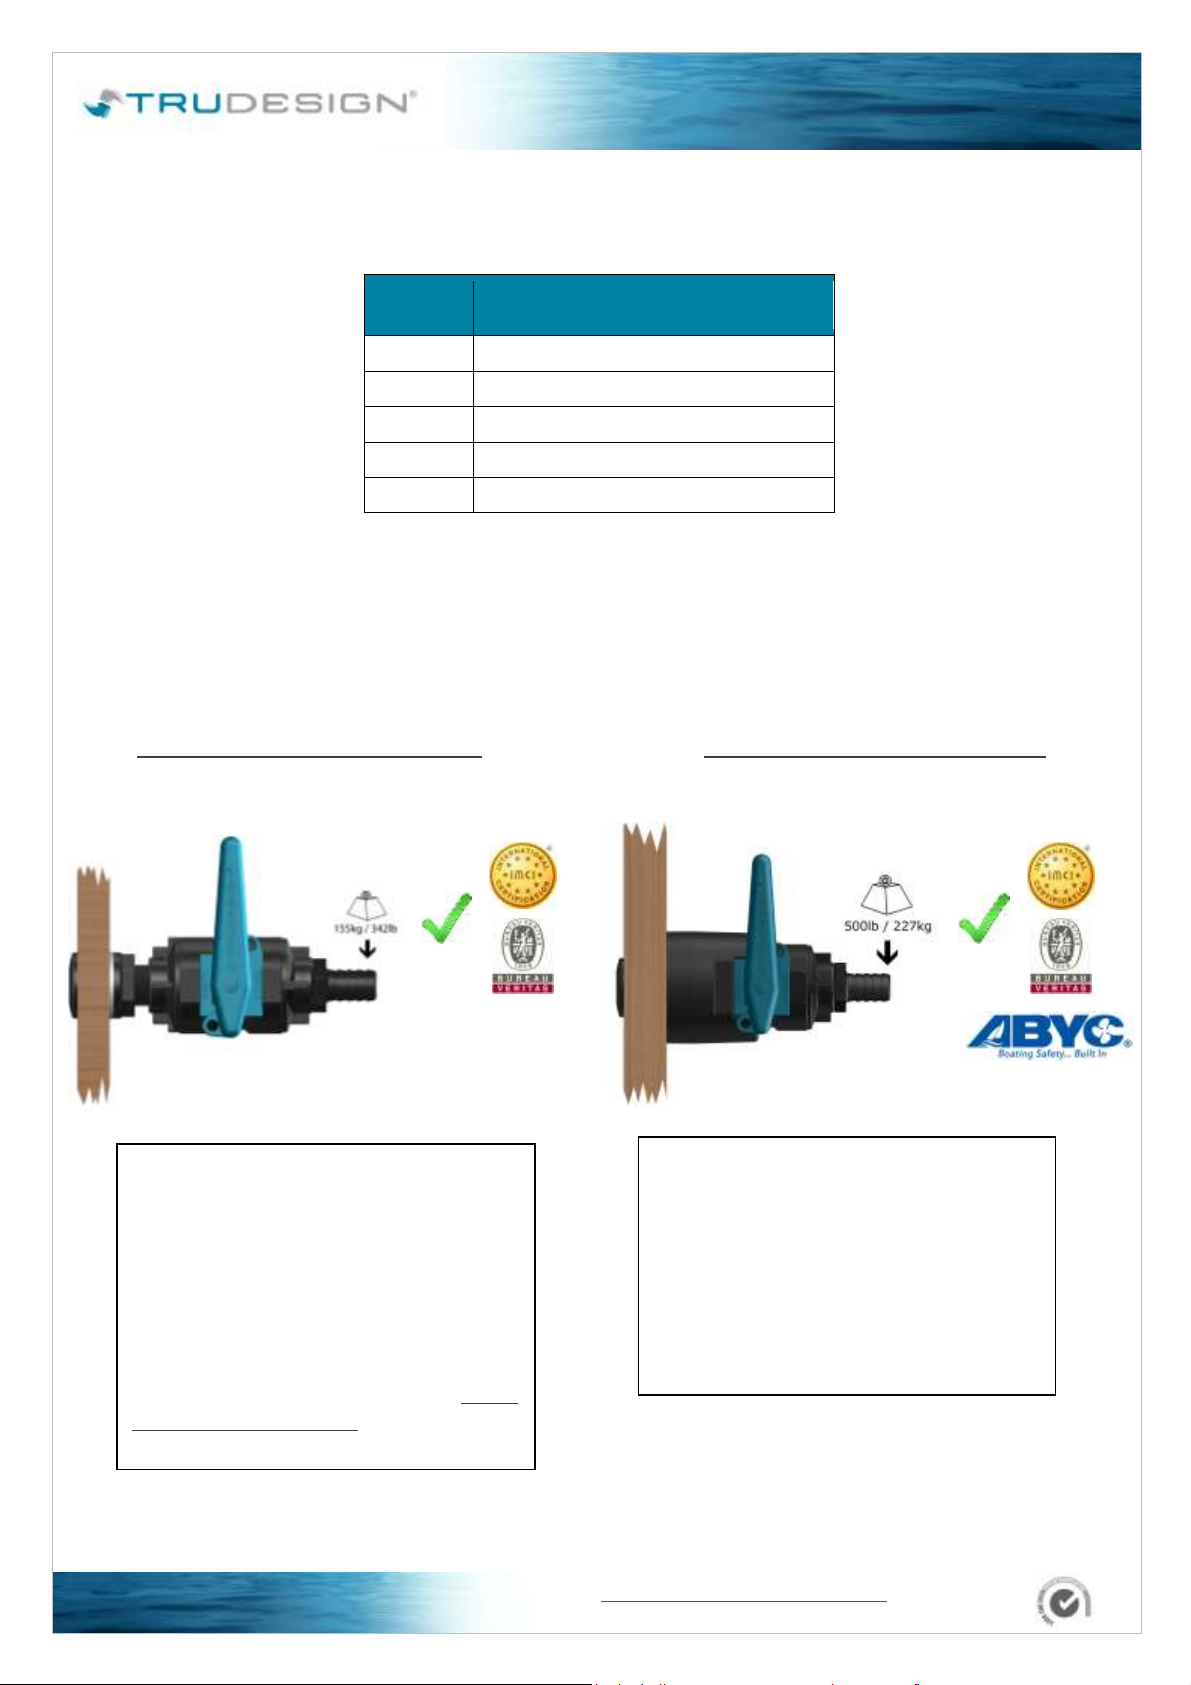
ISO 9093-2 Standard requirements.
ABYC H-27 Standard requirements.
Maximum Hull Thickness:
Size
Maximum Hull Thickness allowing 70%
thread engagement into Ball Valve
½” BSP
36mm
¾” BSP
36mm
1” BSP
36mm
1¼” BSP
49mm
1½” BSP
49mm
Note; it is recommended for very thin hulls that a backing plate be added to make the “effective hull thickness” a
minimum of 20mm.
Standards & Approvals:
.
+
In accordance with ISO 9093-2 standards,
Skin Fittings (Thru Hulls) are subjected to a
155kg (341.7lb) load, applied to the
threaded section for a minimum of 30
seconds, without any damage occurring.
TruDesign Skin Fittings (Thru Hulls) meet
this standard.
Note: ½” size Skin Fitting (Thru Hulls) are
not approved to ISO 9093-2 or ABYC unless
used with an ABYC collar.
TruDesign Skin Fittings (Thru Hulls), when
assembled together with TruDesign Ball
Valves and Load Bearing Collars, comply
with ABYC H-27 standards. This allows the
entire assembly to withstand a 500lb
(226.8kg) load applied to the inboard end
of the assembly (i.e. from the Ball Valve’s
Tail fitting) for a minimum of 30 seconds
without any damage occurring
Page 5
PRODUCT
INFORMATION
LEADERS IN MARI N E COMPO SIT E FI TTING S
www.trudesignplastics.com Rev E
Installation: Location & Drilling
• Ensure there is sufficient room on the inside of the boat to allow the Ball Valve to be screwed on without
hitting the bulkhead or other part of the hull and will not cause the valve handle to be knocked open or
closed. Note; A “T” handle Ball Valve is available for smaller area locations
• Drill from the inside a pilot hole 3mm in diameter, then drill from the outside of the hull a recess that is 1mm
larger in diameter than the flanged head of the chosen Skin Fitting. Only drill deep enough to allow the
flange of the Skin Fitting to sit in the recess flush with the outside of the hull. A hole-saw can be used to cut
the recess and a chisel used to remove the material.
• Making the skin fitting hole. Drill through the centre a hole that is 1mm larger in diameter than the outside
diameter of the thread of the chosen Skin Fitting. A packer may be required to provide a stronger and flat
surface for the nut and washer on the inside of the hull. For very thin hulls a backing plate needs to be added
to make the “effective hull thickness” a minimum of 20mm.
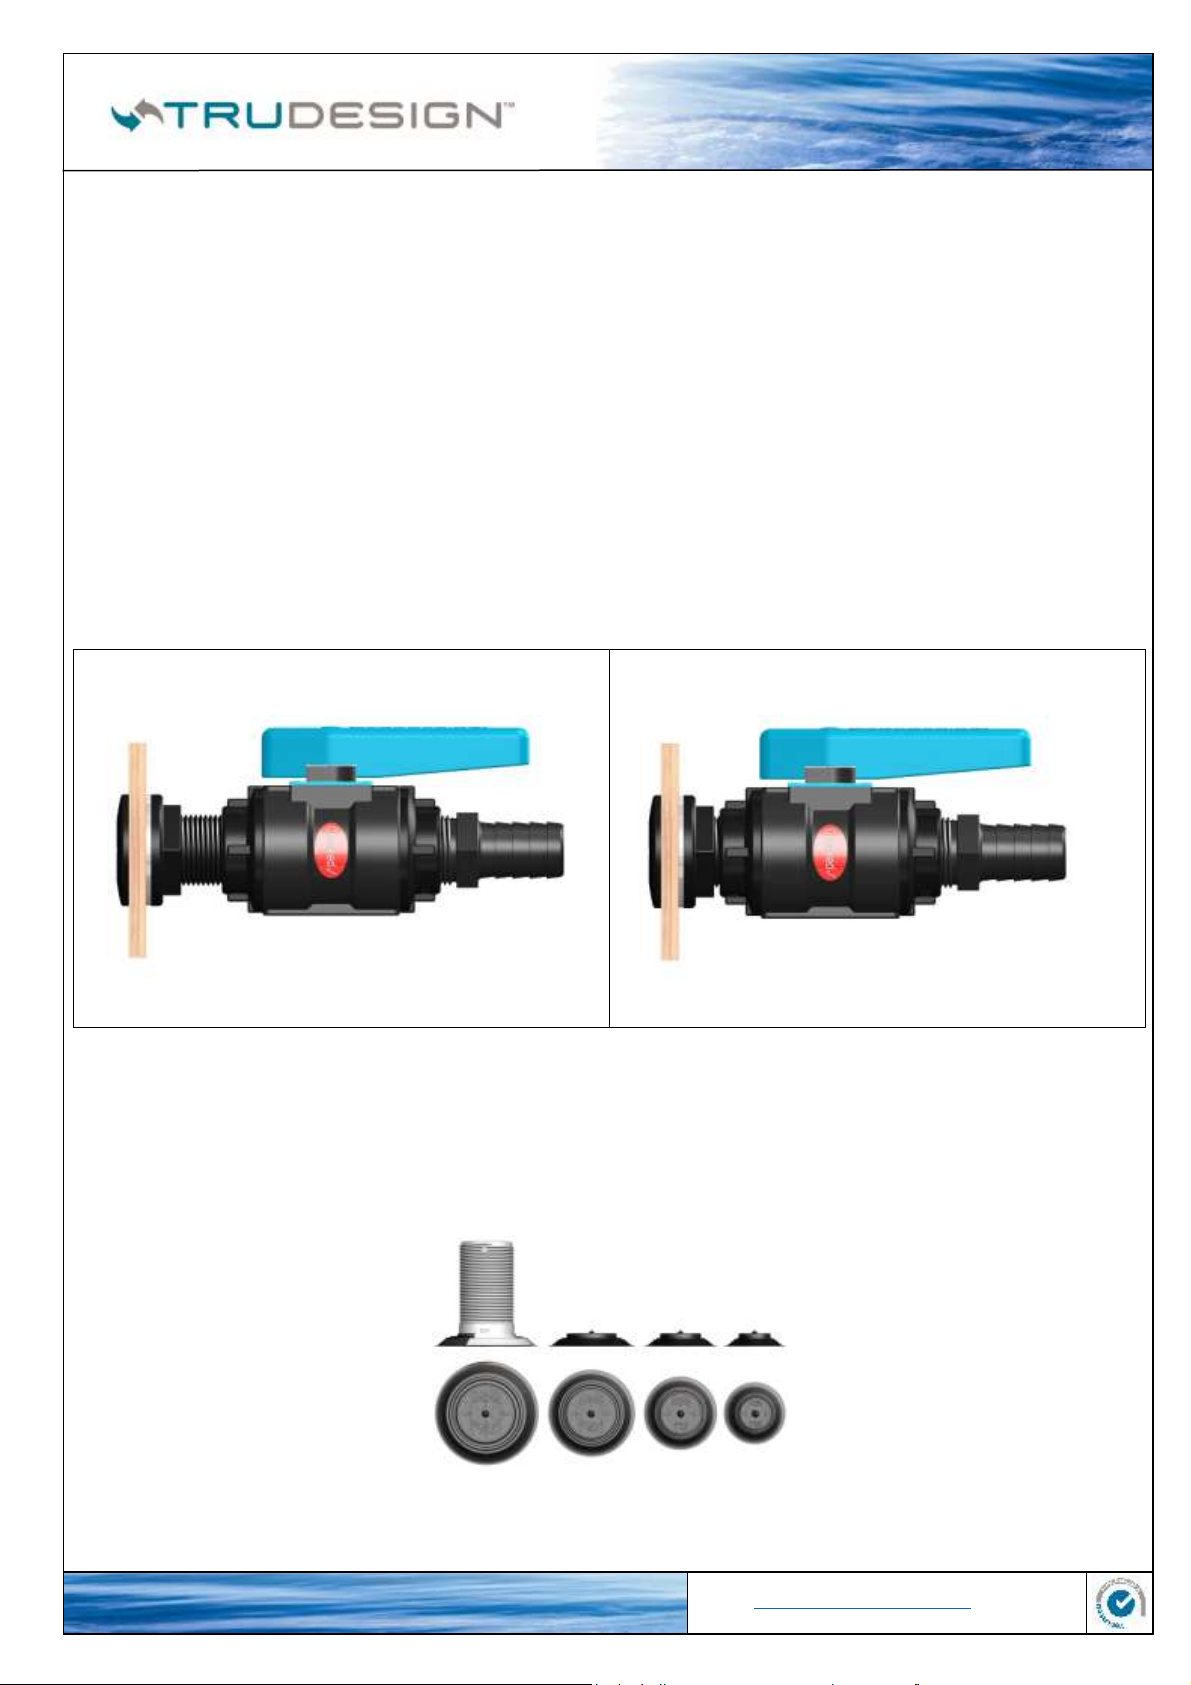
• It is recommended to “dry fit” the Ball Valve Skin fitting assembly and then trim the skin fitting (with a
hacksaw) to allow a 2mm to 5mm gap between Skin Fitting Nut and Ball Valve to minimise overhang.
Too Much Gap between Skin Fitting Nut and Ball Valve
Correct amount of gap between nut and Ball Valve
• TruDesign Skin Fittings (Thru Hull) are suitable for installation in all types of hull construction; steel,
aluminium, composite, fibreglass – cored and solid, wood, wooden sandwich and caulked solid wood hulls.
Ensure fittings are always installed in the centre of individual planks
• For boat builders of GRP and vacuum moulded hulls a disposable mould plug is available that automatically
“shapes” the hull to the recess of the skin fitting and provide a location centre hole – See separate
information sheet. – GRP Mould Plugs
Page 6
PRODUCT
INFORMATION
LEADERS IN MARI N E COMPO SIT E FI TTING S
www.trudesignplastics.com Rev E
Recommended Hull Adhesive Sealants & Glues.
First clean all surfaces to be bonded with a general-purpose cleaner.
• 3M™ Marine Adhesive Sealant Fast Cure 5200. A one-part polyurethane adhesive/sealant. Starts to cure
(tack-free) in approximately 2 hours, after which hoses can be attached. Full cure takes 24 hours – refer to
manufacturer’s product literature.
• SIKAFLEX® 291i and 591 Marine Sealants. Refer to manufacturer’s product literature.
• Bostik® 920 Marine Sealant. A one-part urethane adhesive/sealant. Starts to cure (tack-free) in approx. 2
hours, after which hoses can be attached. Full cure takes 1.5 – 3 days – refer to manufacturer’s product
literature.
• West System® (or similar) two-pot epoxy that mixes to a paste. Tip – adding filler to the West System® will
increase the viscosity and help minimise “running” of the epoxy. Visit http://www.westsystem.com/ss/fillerselection-guide/ for more details.
Fitting & Sealing
• Smear the adhesive or glue on the underside of the Skin Fitting (Thru Hull) flange and a small way up the
thread, but no further than the thickness of the hull. It is important not to have any adhesive on the exposed
thread area as this could prevent the Nut or Ball Valve from turning.
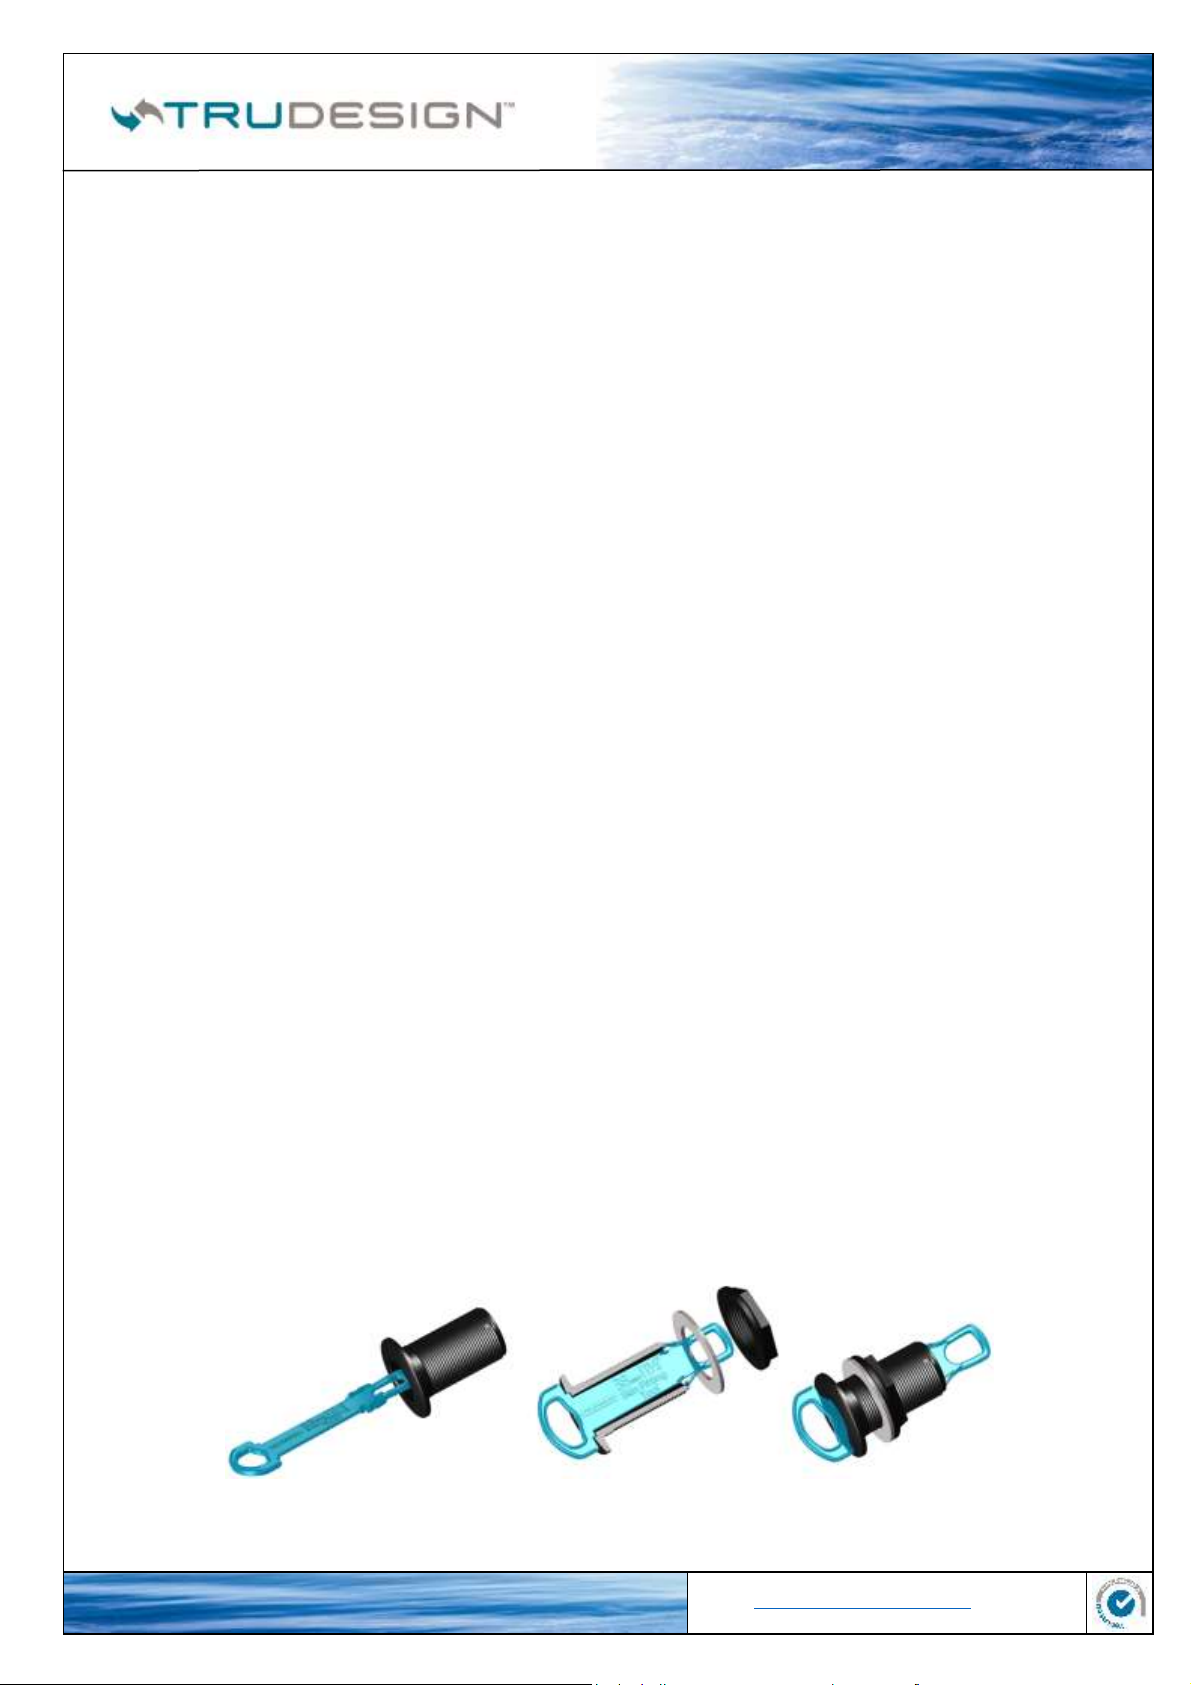
• Insert the Skin Fitting (Thru Hull) through the hull from the outside. Note The TruDesign Skin Fitting
Installation Tool enables our skin fittings to be installed by one person saving time and money. See separate
information sheet on our web site.
• If necessary, place two strips of masking tape over the flange and attach to the hull to temporarily hold in
place. Go inside the hull to fit the Nut. Note it is good practice to have a backing plate to spread the load
especially if there is excessive curvature in the hull or the hull is very thin.
• Hold the thread down near the washer and screw on the Nut. Once the nut is screwed down far enough that
you can hold the fitting above the nut do so and continue to screw the nut down onto the washer ensuring it
is only finger tight.
• On the outside of the hull clean off any excess adhesive. Tip – use an angled tool or putty knife to ‘blend’
adhesive around the Skin Fitting (Thru Hull) flange and the hull so it is easier to clean when sanding and
antifouling in the future.
• After recommended curing times, tighten the nut to no more than 15 ft / lb. There is no need to over-tighten
the Nut, especially if epoxy has been used, as the Skin Fitting (Thru Hull) is now an integral part of the hull.
Page 7
PRODUCT
INFORMATION
LEADERS IN MARI N E COMPO SIT E FI TTING S
www.trudesignplastics.com Rev E
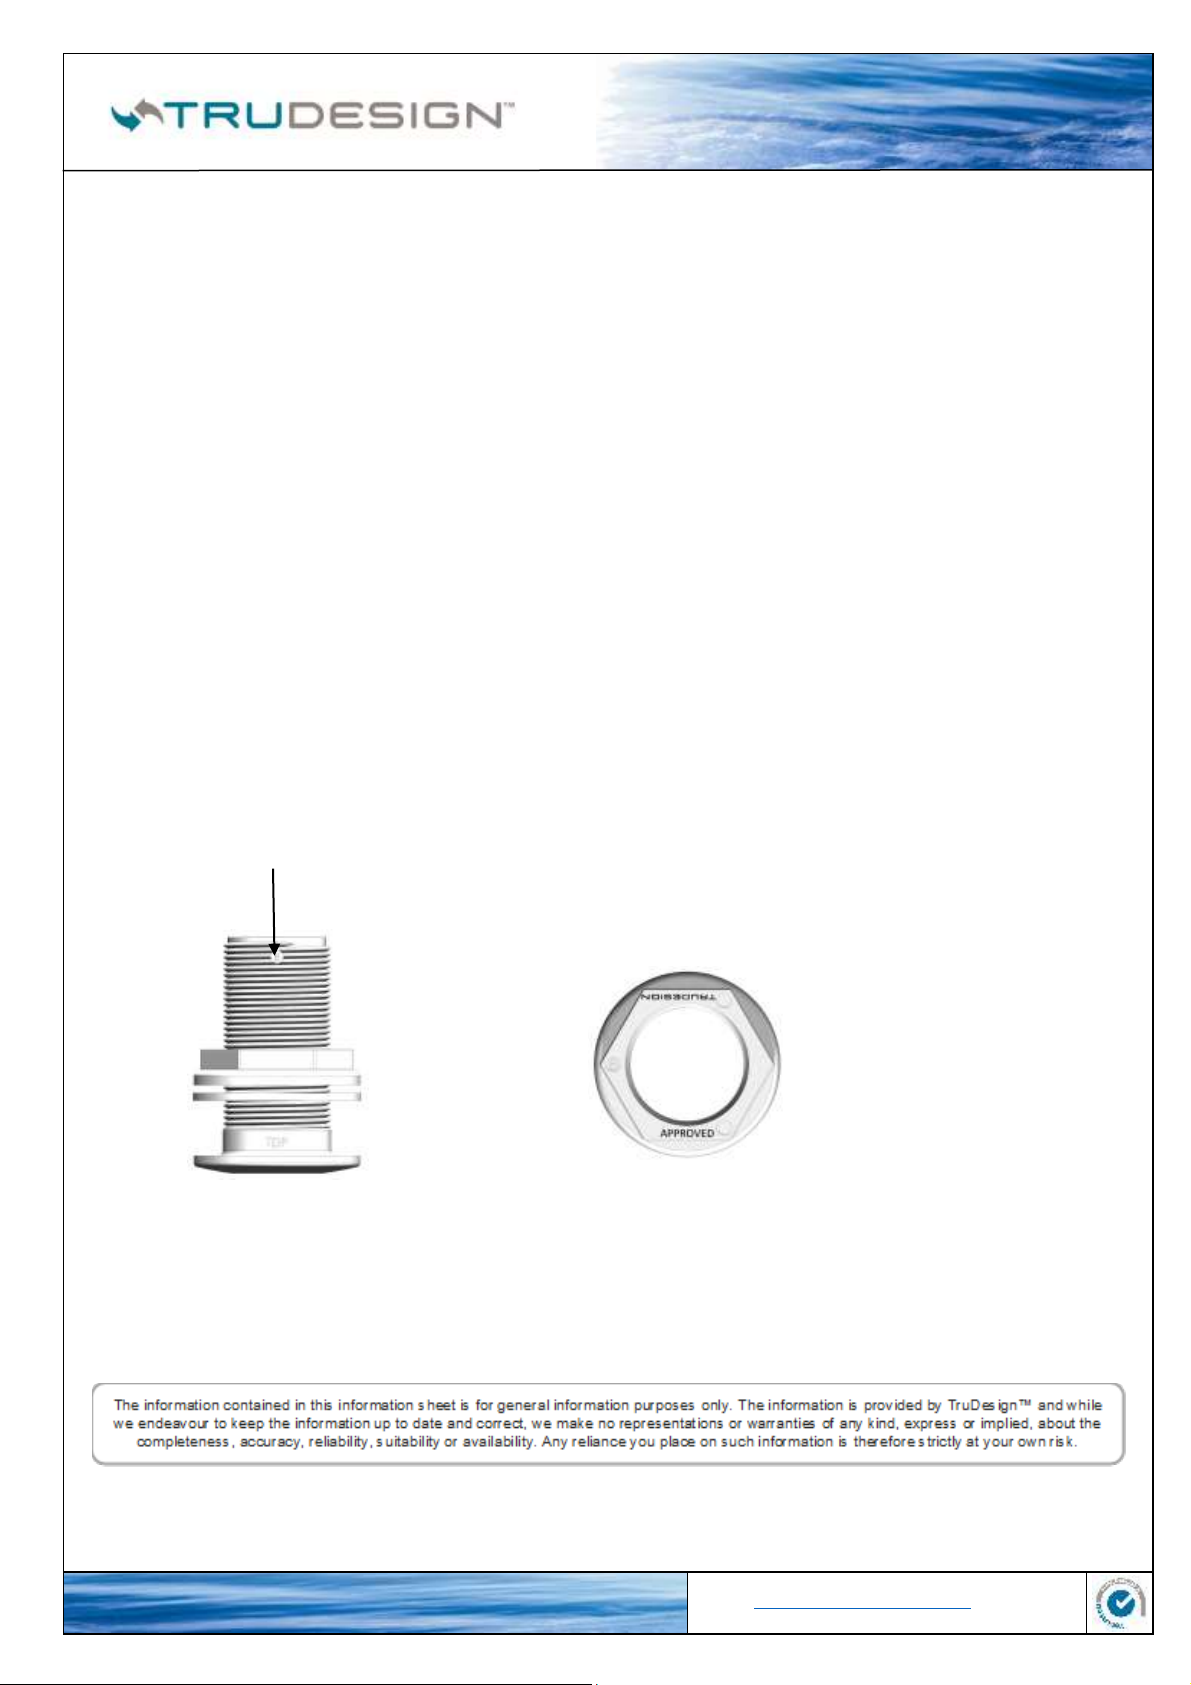
Engraved ‘B’ for BSP thread, or
‘N’ for NPS thread
TruDesign brand is printed on the nut. This
enables clear identification that genuine
fittings are installed.
Thread Sealing
• All the sealants mentioned above under “Hull Adhesives” can be used for thread sealing. These adhesive
sealants allow the Ball valve to be “set in position” to suit handle operation with no risk of turning when in
use. If in the unlikely event the Ball Valve has to be removed this will require significant force.
• 3M™ Marine Adhesive Sealant Fast Cure 4200 is approximately half the strength (once cured) of 3M 5200
which allows for eventual disassembly of the ball valve from skin fitting.
• LOCTITE® 5331 A one-part acetoxy silicone sealant. Starts to cure (tack-free) in approx. 10 minutes, after
which hoses can be attached. Full cure is achieved within 12 hours (at min. 40% atmospheric humidity) –
refer to product literature. Creates a permanent seal for threaded connections.
• PTFE (Teflon) Thread Tape is a traditional thread sealing method which provides a good seal when applied
correctly. However, in some cases if the position or tightness of the Ball Valve is incorrect, it will need to be
unscrewed and more tape applied, slowing the assembly process. Additionally, the fittings can sometimes be
turned by hand after being installed.
• LOCTITE® 55 Pipe Sealing Cord is a coated multi-filament cord designed as a faster method than Teflon tape
to seal threaded fittings. The main advantage is that a component, for example a Ball Valve, could be
screwed down then screwed back a turn to suit positioning whilst still maintaining a tight seal. This
eliminates the need to remove the entire Ball Valve and apply more tape as with traditional Teflon tape.
TruDesign Skin Fittings (Thru Hulls) are printed and marked with the following information.
 Loading...