

Page 1
300 AC/DC
®
ARCMASTER
INVERTER ARC WELDER
Operating Manual
Art # A-07238
Version No: 1 Issue Date: February 22, 2006 Manual No.: 0-4863
Operating Features:
230V460
V
INVERTER
50
60
Hz
1/3
208
V
Page 2
WE APPRECIATE YOUR BUSINESS!
Congratulations on your new Thermal Arc product. We are proud
to have you as our customer and will strive to provide you with
the best service and reliability in the industry. This product is backed
by our extensive warranty and world-wide service network. To
locate your nearest distributor or service agency call
1-800-752-7621, or visit us on the web at www.Thermalarc.com.
This Operating Manual has been designed to instruct you on the
correct use and operation of your Thermal Arc product. Your
satisfaction with this product and its safe operation is our ultimate
concern. Therefore please take the time to read the entire manual,
especially the Safety Precautions. They will help you to avoid
potential hazards that may exist when working with this product.
YOU ARE IN GOOD COMPANY!
The Brand of Choice for Contractors and Fabricators Worldwide.
Thermal Arc is a Global Brand of Arc Welding Products for
Thermadyne Industries Inc. We manufacture and supply to major
welding industry sectors worldwide including; Manufacturing,
Construction, Mining, Automotive, Aerospace, Engineering, Rural
and DIY/Hobbyist.
We distinguish ourselves from our competition through marketleading, dependable products that have stood the test of time. We
pride ourselves on technical innovation, competitive prices,
excellent delivery, superior customer service and technical support,
together with excellence in sales and marketing expertise.
Above all, we are committed to develop technologically advanced
products to achieve a safer working environment within the welding
industry.
Page 3
WARNINGS
Read and understand this entire Manual and your employer’s safety practices before installing,
operating, or servicing the equipment.
While the information contained in this Manual represents the Manufacturer's best judgement,
the Manufacturer assumes no liability for its use.
ArcMaster 300 AC/DC Inverter Arc Welder
Instruction Manual Number 0-4863 for:
Part Number 10-3074
Published by:
Thermadyne Corporation
82 Benning Street
West Lebanon, New Hampshire, USA 03784
(603) 298-5711
www.thermalarc.com
Copyright 2006 by
Thermadyne Corporation
All rights reserved.
Reproduction of this work, in whole or in part, without written permission of the publisher is prohibited.
The publisher does not assume and hereby disclaims any liability to any party for any
loss or damage caused by any error or omission in this Manual, whether such error
results from negligence, accident, or any other cause.
Publication Date: February 22, 2006
Record the following information for Warranty purposes:
Where Purchased: ___________________________________
Purchase Date: ___________________________________
Equipment Serial #: ___________________________________
i
Page 4
TABLE OF CONTENTS
SECTION 1:
SAFETY INSTRUCTIONS AND WARNINGS ....................................................... 1-1
1.01 Arc Welding Hazards ...................................................................................... 1-1
1.02 Principal Safety Standards ............................................................................. 1-5
1.03 Precautions de Securite en Soudage à L’Arc .................................................. 1-6
1.04 Dangers Relatifs au Soudage à L’Arc .............................................................. 1-6
1.05 Principales Normes de Securite ................................................................... 1-10
1.06 Limited Warranty.......................................................................................... 1-11
SECTION 2:
INTRODUCTION ...................................................................................... 2-1
2.01 How To Use This Manual ................................................................................ 2-1
2.02 Equipment Identification................................................................................. 2-1
2.03 Receipt Of Equipment ..................................................................................... 2-1
2.04 Symbol Chart ................................................................................................. 2-2
2.05 Description ..................................................................................................... 2-3
2.06 Functional Block Diagrams ............................................................................. 2-4
2.07 Transporting Methods .................................................................................... 2-4
SECTION 3:
INSTALLATION ....................................................................................... 3-1
3.01 Environment ................................................................................................... 3-1
3.02 Location ......................................................................................................... 3-1
3.03 Electrical Input Connections ........................................................................... 3-1
3.04 Electrical Input Requirements ........................................................................ 3-2
3.05 Input Power .................................................................................................... 3-3
3.06 High Frequency Introduction .......................................................................... 3-3
3.07 High Frequency Interference .......................................................................... 3-4
3.08 Duty Cycle ...................................................................................................... 3-4
3.09 Specifications ................................................................................................. 3-5
SECTION 4:
OPERATOR CONTROLS ............................................................................. 4-1
4.01 ArcMaster 300 ACDC Controls ....................................................................... 4-1
4.02 Weld Process Selection for ArcMaster 300 ACDC .......................................... 4-3
4.03 Weld Parameter Descriptions for ArcMaster 300 ACDC ................................. 4-4
4.04 Weld Parameters for ArcMaster 300 ACDC .................................................... 4-6
4.05 Power Source Features................................................................................... 4-7
SECTION 5:
SET-UP FOR SMAW (STICK) AND GTAW (TIG) .................................................. 5-1
Page 5
TABLE OF CONTENTS (continued)TABLE OF CONTENTS
SECTION 6:
SEQUENCE OF OPERATION ........................................................................ 6-1
6.01 Stick Welding ................................................................................................. 6-3
6.02 AC or DC HF TIG Welding ............................................................................... 6-3
6.03 Slope Mode Sequence .................................................................................... 6-4
6.04 Slope Mode with repeat sequence .................................................................. 6-4
6.05 Pulse Controls ................................................................................................ 6-5
SECTION 7:
BASIC TIG WELDING GUIDE ....................................................................... 7-1
7.01 Explanation of “Fluttery Arc” when AC TIG Welding on Aluminum................. 7-1
7.02 Electrode Polarity ........................................................................................... 7-2
7.03 Tungsten Electrode Current Ranges ............................................................... 7-2
7.04 Tungsten Electrode Types ............................................................................... 7-2
7.05 Guide for Selecting Filler Wire Diameter ......................................................... 7-3
7.06 Shielding Gas Selection .................................................................................. 7-3
7.07 TIG Welding Parameters for Low Carbon & Low Alloy Steel Pipe .................. 7-3
7.08 Welding Parameters for Aluminum ................................................................ 7-4
7.09 Welding Parameters for Steel ......................................................................... 7-4
SECTION 8:
BASIC ARC WELDING GUIDE ..................................................................... 8-1
8.01 Electrode Polarity ........................................................................................... 8-1
8.02 Effects of Stick Welding Various Materials ..................................................... 8-1
SECTION 9:
ROUTINE MAINTENANCE .......................................................................... 9-1
SECTION 10:
BASIC TROUBLESHOOTING ...................................................................... 10-1
10.01 ........................................................................................TIG Welding Problems
10.02 ......................................................................................Stick Welding Problems
10.03 ..................................................................................... Power Source Problems
SECTION 11:
VOLTAGE REDUCTION DEVICE (VRD) ........................................................... 11-1
11.01 ............................................................................................... VRD Specification
11.02 ............................................................................................... VRD Maintenance
11.03 ........................................................................................ Switching VRD On/Off
SECTION 12:
POWER SOURCE ERROR CODES................................................................. 12-1
Page 6
TABLE OF CONTENTS
SECTION 13:
PARTS LIST ......................................................................................... 13-1
13.01 ..................................................................................... Equipment Identification
13.02 ................................................................................. How To Use This Parts List
LIMITED WARRANTY
WARRANTY SCHEDULE
GLOBAL CUSTOMER SERVICE CONTACT INFORMATION .......................... Inside Rear Cover
Page 7
ARCMASTER 300 ACDC
SECTION 1:
SAFETY INSTRUCTIONS AND WARNINGS
WARNING
PROTECT YOURSELF AND OTHERS FROM POSSIBLE SERIOUS INJURY OR DEATH. KEEP CHILDREN AWAY.
PACEMAKER WEARERS KEEP AWAY UNTIL CONSULTING YOUR DOCTOR. DO NOT LOSE THESE INSTRUCTIONS.
READ OPERATING/INSTRUCTION MANUAL BEFORE INSTALLING, OPERATING OR SERVICING THIS EQUIPMENT.
Welding products and welding processes can cause serious injury or death, or damage to other equipment or property,
if the operator does not strictly observe all safety rules and take precautionary actions.
Safe practices have developed from past experience in the use of welding and cutting. These practices must be
learned through study and training before using this equipment. Some of these practices apply to equipment
connected to power lines; other practices apply to engine driven equipment. Anyone not having extensive
training in welding and cutting practices should not attempt to weld.
Safe practices are outlined in the American National Standard Z49.1 entitled: SAFETY IN WELDING AND CUTTING.
This publication and other guides to what you should learn before operating this equipment are listed at the end of
these safety precautions. HAVE ALL INSTALLATION, OPERATION, MAINTENANCE, AND REPAIR WORK PERFORMED
ONLY BY QUALIFIED PEOPLE.
1.01 Arc Welding Hazards
WARNING
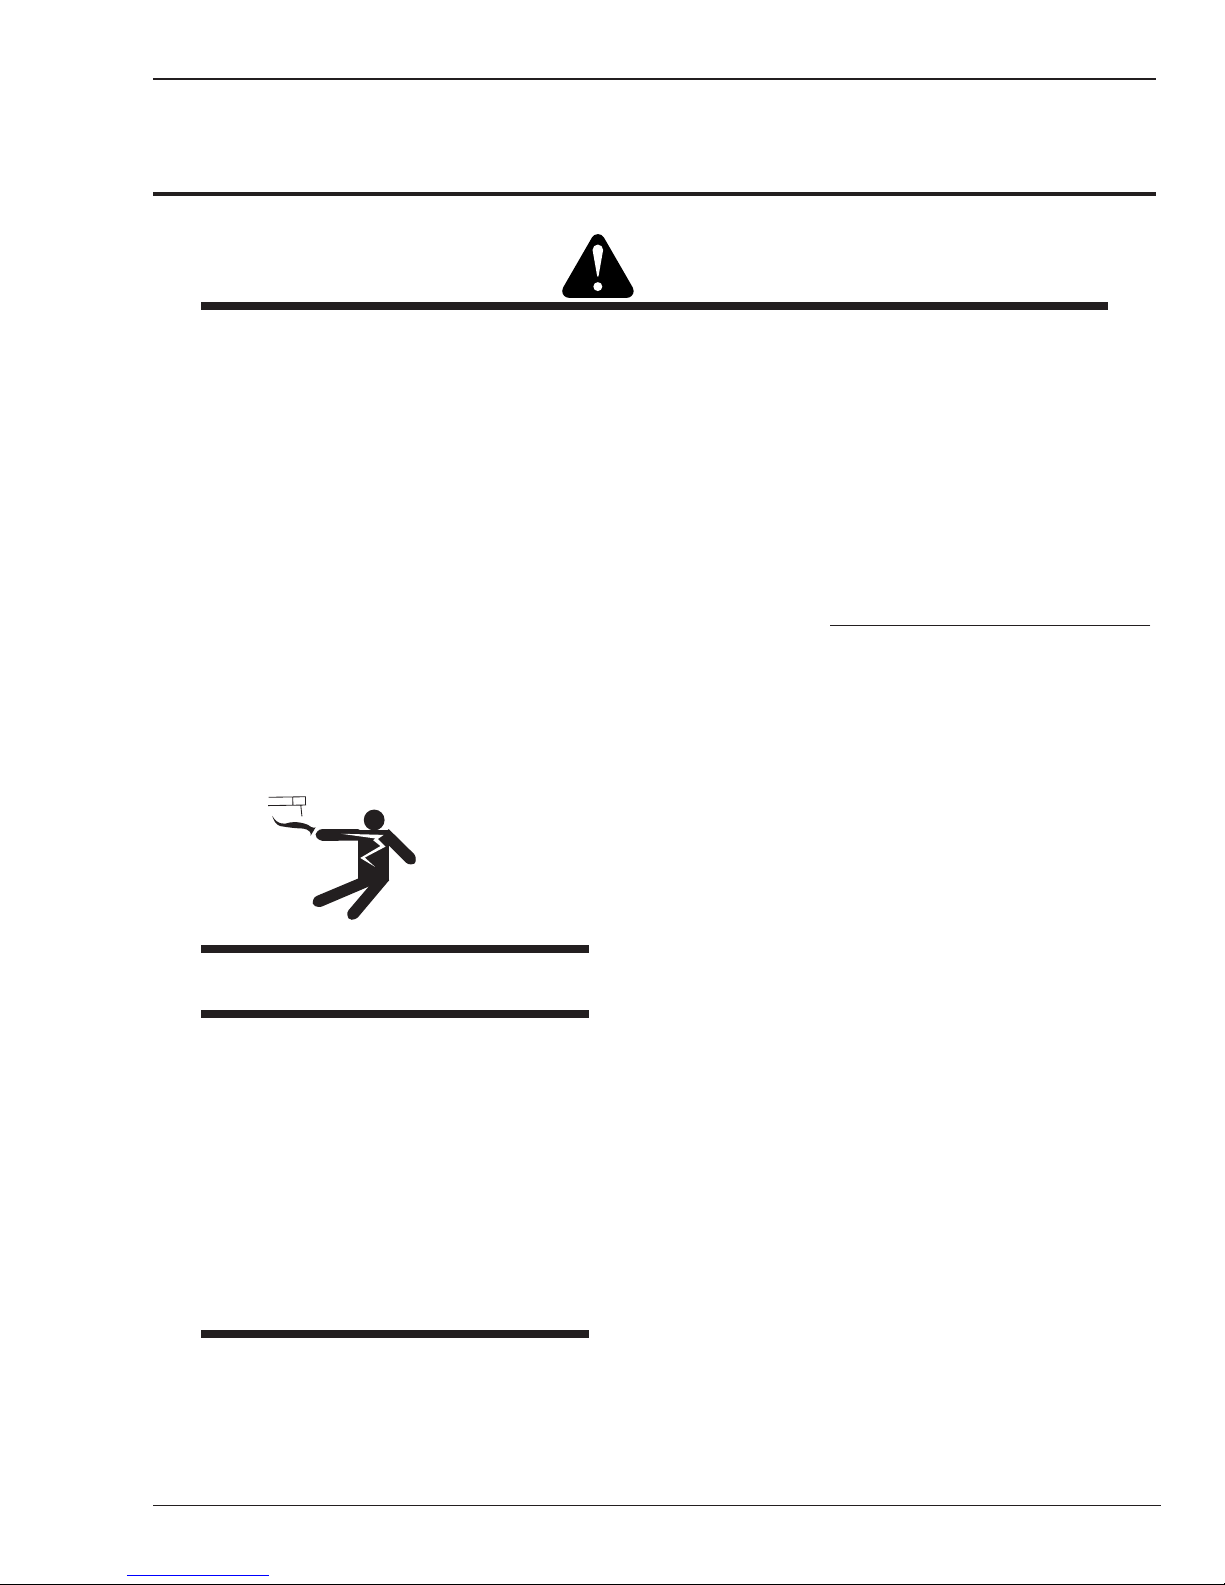
ELECTRIC SHOCK can kill.
Touching live electrical parts can cause fatal
shocks or severe burns. The electrode and
work circuit is electrically live whenever the
output is on. The input power circuit and
machine internal circuits are also live when
power is on. In semiautomatic or automatic
wire welding, the wire, wire reel, drive roll
housing, and all metal parts touching the
welding wire are electrically live. Incorrectly
installed or improperly grounded equipment
is a hazard.
3. Insulate yourself from work and ground using dry
insulating mats or covers.
4. Disconnect input power or stop engine before
installing or servicing this equipment. Lock input
power disconnect switch open, or remove line fuses
so power cannot be turned on accidentally.
5. Properly install and ground this equipment according
to its Owner’s Manual and national, state, and local
codes.
6. Turn off all equipment when not in use. Disconnect
power to equipment if it will be left unattended or out
of service.
7. Use fully insulated electrode holders. Never dip holder
in water to cool it or lay it down on the ground or the
work surface. Do not touch holders connected to two
welding machines at the same time or touch other
people with the holder or electrode.
8. Do not use worn, damaged, undersized, or poorly
spliced cables.
1. Do not touch live electrical parts.
2. Wear dry, hole-free insulating gloves and body
protection.
February 22, 2006
9. Do not wrap cables around your body.
10.Ground the workpiece to a good electrical (earth)
ground.
1-1
Page 8
ARCMASTER 300 ACDC
11.Do not touch electrode while in contact with the work
(ground) circuit.
12. Use only well-maintained equipment. Repair or replace
damaged parts at once.
13.In confined spaces or damp locations, do not use a
welder with AC output unless it is equipped with a
voltage reducer. Use equipment with DC output.
14.Wear a safety harness to prevent falling if working
above floor level.
15.Keep all panels and covers securely in place.
WARNING
ARC RAYS can burn eyes and skin; NOISE can
damage hearing.
Arc rays from the welding process produce
intense heat and strong ultraviolet rays that
can burn eyes and skin. Noise from some
processes can damage hearing.
4. Wear protective clothing made from durable, flameresistant material (wool and leather) and foot
protection.
5. Use approved ear plugs or ear muffs if noise level is
high.
WARNING
FUMES AND GASES can be hazardous to your
health.
Welding produces fumes and gases. Breathing
these fumes and gases can be hazardous to
your health.
1. Keep your head out of the fumes. Do not breath the
fumes.
2. If inside, ventilate the area and/or use exhaust at the
arc to remove welding fumes and gases.
3. If ventilation is poor, use an approved air-supplied
respirator.
1. Wear a welding helmet fitted with a proper shade of
filter (see ANSI Z49.1 listed in Safety Standards) to
protect your face and eyes when welding or watching.
2. Wear approved safety glasses. Side shields
recommended.
3. Use protective screens or barriers to protect others
from flash and glare; warn others not to watch the
arc.
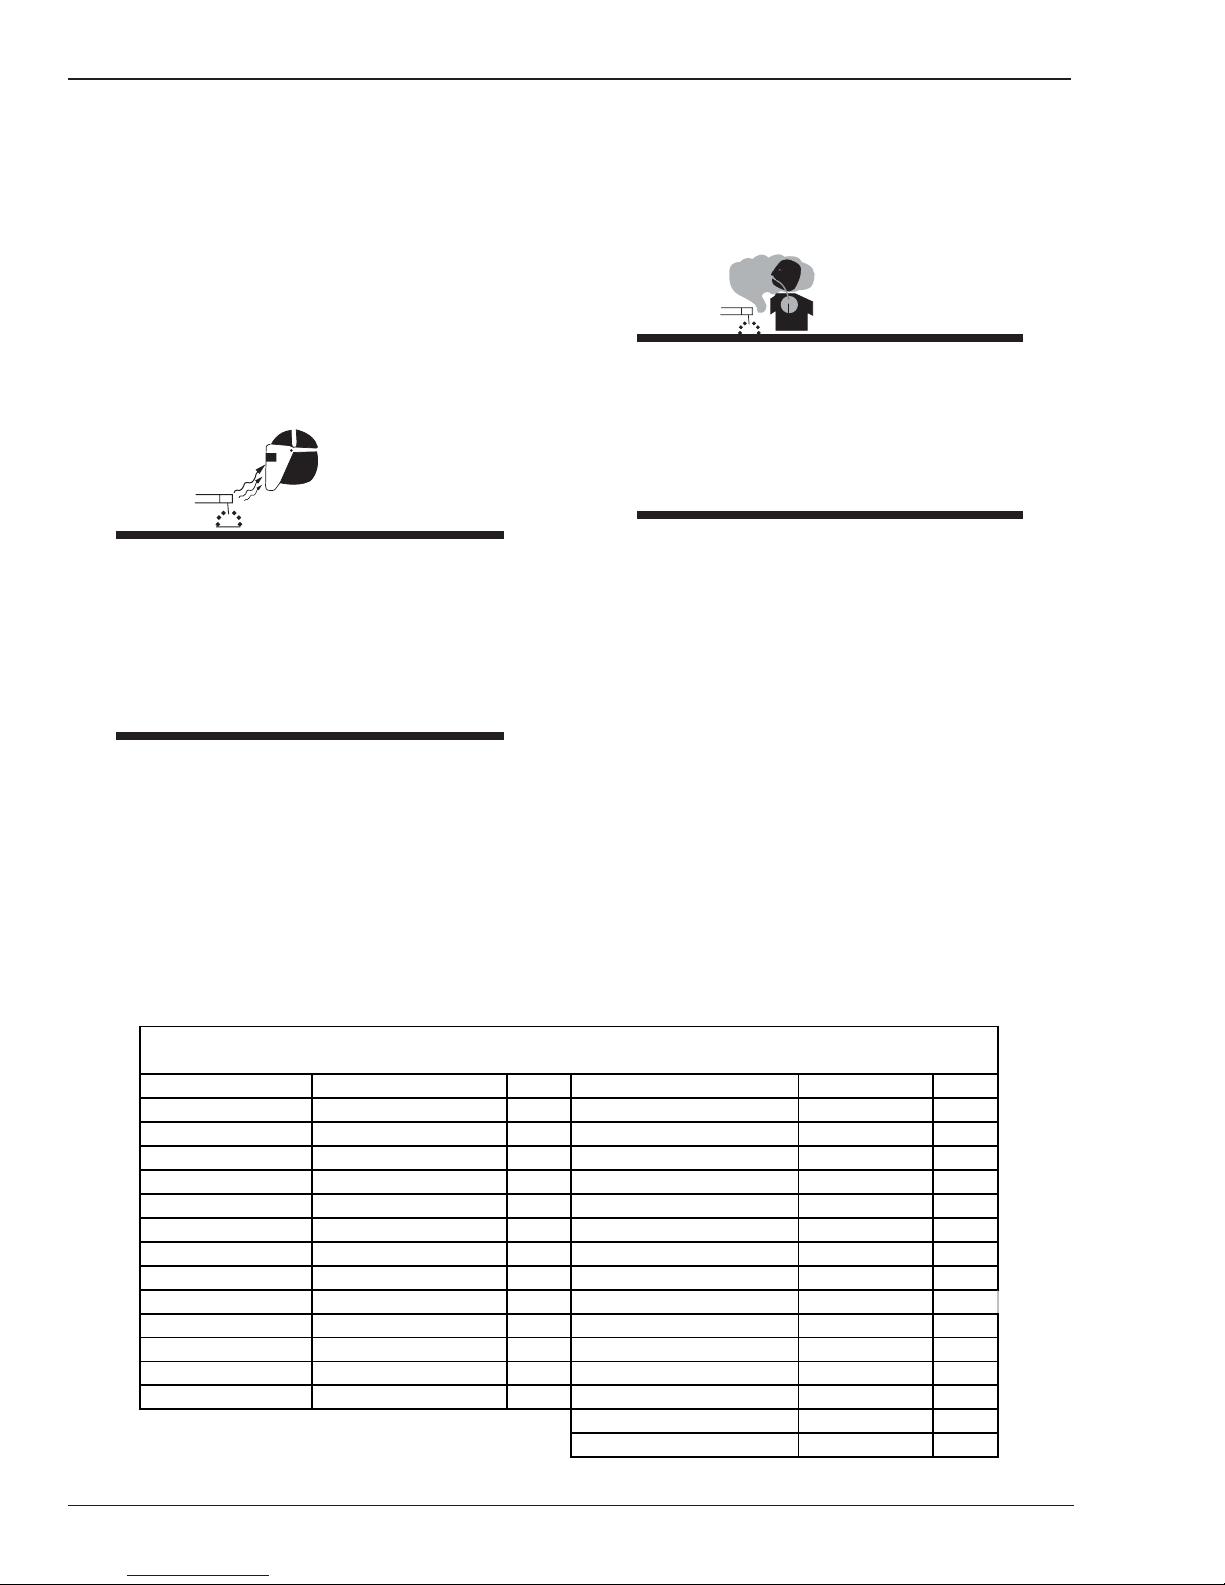
Eye protection filt er shade selector for welding or cutting
(gog gles or helmet), from AWS A6.2-73.
Weldi ng or c utting Electrode Size Filter Weldi ng or c utting Electrode Size Filter
Torch soldering 2
Torch brazing 3 or 4 Non-ferrous base metal All 11
Oxyg en Cutting
Light Under 1 in., 25 mm 3 or 4 Gas tung ste n ar c weldi ng All 12
Medium 1 t o 6 in., 25-150 mm 4 or 5 (T IG) All 12
Heavy Over 6 in., 150 mm 5 or 6 Atomic hydrogen welding All 12
Gas welding
Light Under 1/8 in., 3 mm 4 or 5 Plasma arc welding
M e dium 1 / 8 to 1/2 in. , 3- 12 mm 5 or 6
Heavy Over 1/ 2 in., 12 mm 6 or 8 Light 12
Shielded metal-arc
Under 5/32 in., 4 mm 10 Heavy 14
5/32 to 1/4 in. , 12
Over 1/4 in., 6.4 mm 14 Light Under 300 Amp 9
4. Read the Material Safety Data Sheets (MSDSs) and
the manufacturer’s instruction for metals,
consumables, coatings, and cleaners.
5. Work in a confined space only if it is well ventilated,
or while wearing an air-supplied respirator. Shielding
gases used for welding can displace air causing injury
or death. Be sure the breathing air is safe.
Gas metal-arc
Ferr ous base metal All 12
Carbon arc welding All 12
Carbon arc air g ouging
Pl a sma ar c cutti ng
Medium 300 to 400 Amp 12
Heavy Over 400 Amp 14
1-2
February 22, 2006
Page 9
6. Do not weld in locations near degreasing, cleaning, or
spraying operations. The heat and rays of the arc can
react with vapors to form highly toxic and irritating
gases.
7. Do not weld on coated metals, such as galvanized,
lead, or cadmium plated steel, unless the coating is
removed from the weld area, the area is well ventilated,
and if necessary, while wearing an air-supplied
respirator. The coatings and any metals containing
these elements can give off toxic fumes if welded.
WARNING
WELDING can cause fire or explosion.
ARCMASTER 300 ACDC
WARNING
FLYING SPARKS AND HOT METAL can cause
injury.
Chipping and grinding cause flying metal. As
welds cool, they can throw off slag.
1. Wear approved face shield or safety goggles. Side
shields recommended.
2. Wear proper body protection to protect skin.
WARNING
Sparks and spatter fly off from the welding
arc. The flying sparks and hot metal, weld
spatter, hot workpiece, and hot equipment can
cause fires and burns. Accidental contact of
electrode or welding wire to metal objects can
cause sparks, overheating, or fire.
1. Protect yourself and others from flying sparks and
hot metal.
2. Do not weld where flying sparks can strike flammable
material.
3. Remove all flammables within 35 ft (10.7 m) of the
welding arc. If this is not possible, tightly cover them
with approved covers.
4. Be alert that welding sparks and hot materials from
welding can easily go through small cracks and
openings to adjacent areas.
5. Watch for fire, and keep a fire extinguisher nearby.
6. Be aware that welding on a ceiling, floor, bulkhead, or
partition can cause fire on the hidden side.
7. Do not weld on closed containers such as tanks or
drums.
8. Connect work cable to the work as close to the welding
area as practical to prevent welding current from
traveling long, possibly unknown paths and causing
electric shock and fire hazards.
9. Do not use welder to thaw frozen pipes.
CYLINDERS can explode if damaged.
Shielding gas cylinders contain gas under high
pressure. If damaged, a cylinder can explode.
Since gas cylinders are normally part of the
welding process, be sure to treat them
carefully.
1. Protect compressed gas cylinders from excessive heat,
mechanical shocks, and arcs.
2. Install and secure cylinders in an upright position by
chaining them to a stationary support or equipment
cylinder rack to prevent falling or tipping.
3. Keep cylinders away from any welding or other
electrical circuits.
4. Never allow a welding electrode to touch any cylinder.
5. Use only correct shielding gas cylinders, regulators,
hoses, and fittings designed for the specific
application; maintain them and associated parts in
good condition.
6. Turn face away from valve outlet when opening
cylinder valve.
7. Keep protective cap in place over valve except when
cylinder is in use or connected for use.
8. Read and follow instructions on compressed gas
cylinders, associated equipment, and CGA publication
P-1 listed in Safety Standards.
10.Remove stick electrode from holder or cut off welding
wire at contact tip when not in use.
February 22, 2006
1-3
Page 10
ARCMASTER 300 ACDC
WARNING
Engines can be dangerous.
WARNING
ENGINE EXHAUST GASES can kill.
4. To prevent accidental starting during servicing,
disconnect negative (-) battery cable from battery.
5. Keep hands, hair, loose clothing, and tools away
from moving parts.
6. Reinstall panels or guards and close doors when
servicing is finished and before starting engine.
WARNING
Engines produce harmful exhaust gases.
1. Use equipment outside in open, well-ventilated areas.
2. If used in a closed area, vent engine exhaust outside
and away from any building air intakes.
WARNING
ENGINE FUEL can cause fire or explosion.
Engine fuel is highly flammable.
1. Stop engine before checking or adding fuel.
2. Do not add fuel while smoking or if unit is near any
sparks or open flames.
3. Allow engine to cool before fueling. If possible, check
and add fuel to cold engine before beginning job.
4. Do not overfill tank — allow room for fuel to expand.
5. Do not spill fuel. If fuel is spilled, clean up before
starting engine.
SPARKS can cause BATTERY GASES TO
EXPLODE; BATTERY ACID can burn eyes and
skin.
Batteries contain acid and generate explosive gases.
1. Always wear a face shield when working on a battery.
2. Stop engine before disconnecting or connecting
battery cables.
3. Do not allow tools to cause sparks when working on
a battery.
4. Do not use welder to charge batteries or jump start
vehicles.
5. Observe correct polarity (+ and –) on batteries.
WARNING
STEAM AND PRESSURIZED HOT COOLANT
can burn face, eyes, and skin.
WARNING
MOVING PARTS can cause injury.
Moving parts, such as fans, rotors, and belts can cut
fingers and hands and catch loose clothing.
1. Keep all doors, panels, covers, and guards closed
and securely in place.
2. Stop engine before installing or connecting unit.
3. Have only qualified people remove guards or
covers for maintenance and troubleshooting as
necessary.
1-4
The coolant in the radiator can be very hot
and under pressure.
1. Do not remove radiator cap when engine is hot. Allow
engine to cool.
2. Wear gloves and put a rag over cap area when
removing cap.
3. Allow pressure to escape before completely removing
cap.
February 22, 2006
Page 11
ARCMASTER 300 ACDC
WARNING
This product, when used for welding or
cutting, produces fumes or gases which
contain chemicals know to the State of
California to cause birth defects and, in some
cases, cancer. (California Health & Safety code
Sec. 25249.5 et seq.)
NOTE
Considerations About Welding And The Effects
of Low Frequency Electric and Magnetic Fields
The following is a quotation from the General Conclusions
Section of the U.S. Congress, Office of Technology
Assessment,
Frequency Electric & Magnetic Fields - Background Paper,
OTA-BP-E-63 (Washington, DC: U.S. Government Printing
Office, May 1989): “...there is now a very large volume of
scientific findings based on experiments at the cellular
level and from studies with animals and people which
clearly establish that low frequency magnetic fields and
interact with, and produce changes in, biological systems.
While most of this work is of very high quality, the results
are complex. Current scientific understanding does not
yet allow us to interpret the evidence in a single coherent
framework. Even more frustrating, it does not yet allow
us to draw definite conclusions about questions of
possible risk or to offer clear science-based advice on
strategies to minimize or avoid potential risks.”
To reduce magnetic fields in the workplace, use the
following procedures.
1. Keep cables close together by twisting or taping
them.
Biological Effects of Power
1.02 Principal Safety Standards
Safety in Welding and Cutting, ANSI Standard Z49.1, from
American Welding Society, 550 N.W. LeJeune Rd., Miami,
FL 33126.
Safety and Health Standards, OSHA 29 CFR 1910, from
Superintendent of Documents, U.S. Government Printing
Office, Washington, D.C. 20402.
Recommended Safe Practices for the Preparation for
Welding and Cutting of Containers That Have Held
Hazardous Substances, American Welding Society
Standard AWS F4.1, from American Welding Society, 550
N.W. LeJeune Rd., Miami, FL 33126.
National Electrical Code, NFPA Standard 70, from National
Fire Protection Association, Batterymarch Park, Quincy,
MA 02269.
Safe Handling of Compressed Gases in Cylinders, CGA
Pamphlet P-1, from Compressed Gas Association, 1235
Jefferson Davis Highway, Suite 501, Arlington, VA 22202.
Code for Safety in Welding and Cutting, CSA Standard
W117.2, from Canadian Standards Association, Standards
Sales, 178 Rexdale Boulevard, Rexdale, Ontario, Canada
M9W 1R3.
Safe Practices for Occupation and Educational Eye and
Face Protection, ANSI Standard Z87.1, from American
National Standards Institute, 1430 Broadway, New York,
NY 10018.
Cutting and Welding Processes, NFPA Standard 51B, from
National Fire Protection Association, Batterymarch Park,
Quincy, MA 02269.
2. Arrange cables to one side and away from the
operator.
3. Do not coil or drape cable around the body.
4. Keep welding power source and cables as far away
from body as practical.
ABOUT PACEMAKERS:
The above procedures are among those also
normally recommended for pacemaker
wearers. Consult your doctor for complete
information.
February 22, 2006
1-5
Page 12
ARCMASTER 300 ACDC
1.03 Precautions de Securite en Soudage à L’Arc
MISE EN GARDE
LE SOUDAGE A L’ARC EST DANGEREUX
PROTEGEZ-VOUS, AINSI QUE LES AUTRES, CONTRE LES BLESSURES GRAVES POSSIBLES OU LA MORT. NE LAISSEZ
PAS LES ENFANTS S’APPROCHER, NI LES PORTEURS DE STIMULATEUR CARDIAQUE (A MOINS QU’ILS N’AIENT
CONSULTE UN MEDECIN). CONSERVEZ CES INSTRUCTIONS. LISEZ LE MANUEL D’OPERATION OU LES INSTRUCTIONS AVANT D’INSTALLER, UTILISER OU ENTRETENIR CET EQUIPEMENT.
Les produits et procédés de soudage peuvent sauser des blessures graves ou la mort, de même que des dommages
au reste du matériel et à la propriété, si l’utilisateur n’adhère pas strictement à toutes les règles de sécurité et ne prend
pas les précautions nécessaires.
En soudage et coupage, des pratiques sécuritaires se sont développées suite à l’expérience passée. Ces pratiques
doivent être apprises par étude ou entraînement avant d’utiliser l’equipement. Toute personne n’ayant pas suivi un
entraînement intensif en soudage et coupage ne devrait pas tenter de souder. Certaines pratiques concernent les
équipements raccordés aux lignes d’alimentation alors que d’autres s’adressent aux groupes électrogènes.
La norme Z49.1 de l’American National Standard, intitulée “SAFETY IN WELDING AND CUTTING” présente les pratiques sécuritaires à suivre. Ce document ainsi que d’autres guides que vous devriez connaître avant d’utiliser cet
équipement sont présentés à la fin de ces instructions de sécurité.
SEULES DES PERSONNES QUALIFIEES DOIVENT FAIRE
DES TRAVAUX D’INSTALLATION, DE REPARATION,
D’ENTRETIEN ET D’ESSAI.
1. Ne touchez pas à des pièces sous tension.
2. Portez des gants et des vêtements isolants, secs et
non troués.
1.04 Dangers Relatifs au Soudage à L’Arc
AVERTISSEMENT
L’ELECTROCUTION PEUT ETRE MORTELLE.
Une décharge électrique peut tuer ou brûler
gravement. L’électrode et le circuit de soudage
sont sous tension dès la mise en circuit. Le
circuit d’alimentation et les circuits internes
de l’équipement sont aussi sous tension dès
la mise en marche. En soudage automatique
ou semi-automatique avec fil, ce dernier, le
rouleau ou la bobine de fil, le logement des
galets d’entrainement et toutes les pièces
métalliques en contact avec le fil de soudage
sont sous tension. Un équipement
inadéquatement installé ou inadéquatement
mis à la terre est dangereux.
1-6
3 Isolez-vous de la pièce à souder et de la mise à la
terre au moyen de tapis isolants ou autres.
4. Déconnectez la prise d’alimentation de l’équipement
ou arrêtez le moteur avant de l’installer ou d’en faire
l’entretien. Bloquez le commutateur en circuit ouvert
ou enlevez les fusibles de l’alimentation afin d’éviter
une mise en marche accidentelle.
5. Veuillez à installer cet équipement et à le mettre à la
terre selon le manuel d’utilisation et les codes
nationaux, provinciaux et locaux applicables.
6. Arrêtez tout équipement après usage. Coupez
l’alimentation de l’équipement s’il est hors d’usage
ou inutilisé.
7. N’utilisez que des porte-électrodes bien isolés. Ne
jamais plonger les porte-électrodes dans l’eau pour
les refroidir. Ne jamais les laisser traîner par terre ou
sur les pièces à souder. Ne touchez pas aux porteélectrodes raccordés à deux sources de courant en
même temps. Ne jamais toucher quelqu’un d’autre
avec l’électrode ou le porte-électrode.
8. N’utilisez pas de câbles électriques usés,
endommagés, mal épissés ou de section trop petite.
9. N’enroulez pas de câbles électriques autour de votre
corps.
February 22, 2006
Page 13
ARCMASTER 300 ACDC
10.N’utilisez qu’une bonne prise de masse pour la mise à
la terre de la pièce à souder.
11.Ne touchez pas à l’électrode lorsqu’en contact avec le
circuit de soudage (terre).
12.N’utilisez que des équipements en bon état. Réparez
ou remplacez aussitôt les pièces endommagées.
13.Dans des espaces confinés ou mouillés, n’utilisez pas
de source de courant alternatif, à moins qu’il soit muni
d’un réducteur de tension. Utilisez plutôt une source
de courant continu.
14. Portez un harnais de sécurité si vous travaillez en hauteur.
15.Fermez solidement tous les panneaux et les capots.
AVERTISSEMENT
LE RAYONNEMENT DE L’ARC PEUT BRÛLER
LES YEUX ET LA PEAU; LE BRUIT PEUT
ENDOMMAGER L’OUIE.
L’arc de soudage produit une chaleur et des
rayons ultraviolets intenses, susceptibles de
brûler les yeux et la peau. Le bruit causé par
certains procédés peut endommager l’ouïe.
1. Portez une casque de soudeur avec filtre oculaire de
nuance appropriée (consultez la norme ANSI Z49
indiquée ci-après) pour vous protéger le visage et les
yeux lorsque vous soudez ou que vous observez
l’exécution d’une soudure.
2. Portez des lunettes de sécurité approuvées. Des écrans
latéraux sont recommandés.
3. Entourez l’aire de soudage de rideaux ou de cloisons
pour protéger les autres des coups d’arc ou de
l’éblouissement; avertissez les observateurs de ne pas
regarder l’arc.
4. Portez des vêtements en matériaux ignifuges et
durables (laine et cuir) et des chaussures de sécurité.
5. Portez un casque antibruit ou des bouchons d’oreille
approuvés lorsque le niveau de bruit est élevé.
AVERTISSEMENT
LES VAPEURS ET LES FUMEES SONT
DANGEREUSES POUR LA SANTE.
Le soudage dégage des vapeurs et des fumées
dangereuses à respirer.
SELECTION DES NUANCES DE FILTRES OCULAIRS POUR LA PROTECTION
DES YEUX EN COUPAGE ET SOUDAGE (selon AWS á 8.2-73)
Opération de coupage
ou soudage
Brassage tendre
au chalumeau
Brassage fort
au chalumeau
Oxycoupage métaux ferreux tout es condit ions 12
moyen de 1 á 6 po. (25 á 150 mm) 4 ou 5
Soudage aux gaz Soudage á l'arc Plasma (PAW) tout es dimensions 12
moyen de 1/8 á 1/2 po. (3 á 12 mm) 5 ou 6 mince 12
Soudage á l'arc avec
électrode enrobees
(SMAW)
Dimension d'électr ode ou
Epiasseur de métal ou
Intensité de courant
toutes conditions 2
tout es condit ions 3 ou 4 métaux non- ferreux toutes condit ions 11
mince moins de 1 po. (25 mm) 2 ou 3
épais plus de 6 po. (150 mm) 5 ou 6
mince moins de 1/8 po. ( 3 mm) 4 ou 5
épais plus de 1/2 po. (12 mm) 6 ou 8 épais 14
moins de 5/32 po. (4 mm) 10 Coupage á l'arc Plasma (PAC)
5/32 á 1/ 4 po. ( 4 á 6.4 mm) 12 mince moins de 300 amperès 9
plus de 1/4 po. (6.4 mm) 14 moyen de 300 á 400 amperès 12
Nuance de
fi l tre oculaire
Opération de coupage
ou soudage
Soudage á l'arc sous gaz
avec fil plein (GMAW)
Soudage á l'arc sous gaz avec
élect r ode de t ungstène (GTAW )
Soudage á l'hydrogène
at omique (AHW )
Soudage á l'arc avec
élect r ode de car bone (CAW)
Gougeage A i r - Arc avec
élect r ode de car bone
Dimension d'électrode ou
Epiasseur de métal ou
Intensité de courant
toutes conditions 12
toutes conditions 12
toutes conditions 12
épais plus d e 400 am perès 14
Nuance de
fi l tre oculaire
February 22, 2006
1-7
Page 14
ARCMASTER 300 ACDC
1. Eloignez la tête des fumées pour éviter de les respirer.
2. A l’intérieur, assurez-vous que l’aire de soudage est
bien ventilée ou que les fumées et les vapeurs sont
aspirées à l’arc.
3. Si la ventilation est inadequate, portez un respirateur
à adduction d’air approuvé.
4. Lisez les fiches signalétiques et les consignes du
fabricant relatives aux métaux, aux produits
consummables, aux revêtements et aux produits
nettoyants.
5. Ne travaillez dans un espace confiné que s’il est bien
ventilé; sinon, portez un respirateur à adduction d’air.
Les gaz protecteurs de soudage peuvent déplacer
l’oxygène de l’air et ainsi causer des malaises ou la
mort. Assurez-vous que l’air est propre à la respiration.
6. Ne soudez pas à proximité d’opérations de
dégraissage, de nettoyage ou de pulvérisation. La
chaleur et les rayons de l’arc peuvent réagir avec des
vapeurs et former des gaz hautement toxiques et irritants.
7. Ne soudez des tôles galvanisées ou plaquées au plomb
ou au cadmium que si les zones à souder ont été
grattées à fond, que si l’espace est bien ventilé; si
nécessaire portez un respirateur à adduction d’air. Car
ces revêtements et tout métal qui contient ces
éléments peuvent dégager des fumées toxiques au
moment du soudage.
1. Protégez-vous, ainsi que les autres, contre les
étincelles et du métal chaud.
2. Ne soudez pas dans un endroit où des particules
volantes ou des projections peuvent atteindre des
matériaux inflammables.
3. Enlevez toutes matières inflammables dans un rayon
de 10, 7 mètres autour de l’arc, ou couvrez-les
soigneusement avec des bâches approuvées.
4. Méfiez-vous des projections brulantes de soudage
susceptibles de pénétrer dans des aires adjacentes
par de petites ouvertures ou fissures.
5. Méfiez-vous des incendies et gardez un extincteur à
portée de la main.
6. N’oubliez pas qu’une soudure réalisée sur un plafond,
un plancher, une cloison ou une paroi peut enflammer
l’autre côté.
7. Ne soudez pas un récipient fermé, tel un réservoir ou
un baril.
8. Connectez le câble de soudage le plus près possible
de la zone de soudage pour empêcher le courant de
suivre un long parcours inconnu, et prévenir ainsi les
risques d’électrocution et d’incendie.
9. Ne dégelez pas les tuyaux avec un source de courant.
10.Otez l’électrode du porte-électrode ou coupez le fil au
tube-contact lorsqu’inutilisé après le soudage.
11.Portez des vêtements protecteurs non huileux, tels
des gants en cuir, une chemise épaisse, un pantalon
revers, des bottines de sécurité et un casque.
AVERTISSEMENT
LE SOUDAGE PEUT CAUSER UN INCENDIE OU
UNE EXPLOSION
L’arc produit des étincellies et des projections.
Les particules volantes, le métal chaud, les
projections de soudure et l’équipement
surchauffé peuvent causer un incendie et des
brûlures. Le contact accidentel de l’électrode
ou du fil-électrode avec un objet métallique
peut provoquer des étincelles, un
échauffement ou un incendie.
1-8
AVERTISSEMENT
LES ETINCELLES ET LES PROJECTIONS
BRULANTES PEUVENT CAUSER DES
BLESSURES.
Le piquage et le meulage produisent des
particules métalliques volantes. En
refroidissant, la soudure peut projeter du
éclats de laitier.
1. Portez un écran facial ou des lunettes protectrices
approuvées. Des écrans latéraux sont
recommandés.
2. Portez des vêtements appropriés pour protéger
la peau.
February 22, 2006
Page 15
ARCMASTER 300 ACDC
1. Utilisez l’équipement à l’extérieur dans des aires
ouvertes et bien ventilées.
AVERTISSEMENT
LES BOUTEILLES ENDOMMAGEES PEUVENT
EXPLOSER
Les bouteilles contiennent des gaz protecteurs
sous haute pression. Des bouteilles
endommagées peuvent exploser. Comme les
bouteilles font normalement partie du procédé
de soudage, traitez-les avec soin.
1. Protégez les bouteilles de gaz comprimé contre les
sources de chaleur intense, les chocs et les arcs de
soudage.
2. Enchainez verticalement les bouteilles à un support
ou à un cadre fixe pour les empêcher de tomber ou
d’être renversées.
3. Eloignez les bouteilles de tout circuit électrique ou de
tout soudage.
4. Empêchez tout contact entre une bouteille et une
électrode de soudage.
2. Si vous utilisez ces équipements dans un endroit
confiné, les fumées d’échappement doivent être
envoyées à l’extérieur, loin des prises d’air du bâtiment.
AVERTISSEMENT
LE CARBURANT PEUR CAUSER UN INCENDIE
OU UNE EXPLOSION.
Le carburant est hautement inflammable.
1. Arrêtez le moteur avant de vérifier le niveau e
carburant ou de faire le plein.
2. Ne faites pas le plein en fumant ou proche d’une source
d’étincelles ou d’une flamme nue.
3. Si c’est possible, laissez le moteur refroidir avant de
faire le plein de carburant ou d’en vérifier le niveau au
début du soudage.
4. Ne faites pas le plein de carburant à ras bord: prévoyez
de l’espace pour son expansion.
5. N’utilisez que des bouteilles de gaz protecteur, des
détendeurs, des boyauxs et des raccords conçus pour
chaque application spécifique; ces équipements et les
pièces connexes doivent être maintenus en bon état.
6. Ne placez pas le visage face à l’ouverture du robinet
de la bouteille lors de son ouverture.
7. Laissez en place le chapeau de bouteille sauf si en
utilisation ou lorsque raccordé pour utilisation.
8. Lisez et respectez les consignes relatives aux bouteilles
de gaz comprimé et aux équipements connexes, ainsi
que la publication P-1 de la CGA, identifiée dans la
liste de documents ci-dessous.
AVERTISSEMENT
LES MOTEURS PEUVENT ETRE DANGEREUX
LES GAZ D’ECHAPPEMENT DES MOTEURS
PEUVENT ETRE MORTELS.
5. Faites attention de ne pas renverser de carburant.
Nettoyez tout carburant renversé avant de faire
démarrer le moteur.
AVERTISSEMENT
DES PIECES EN MOUVEMENT PEUVENT
CAUSER DES BLESSURES.
Des pièces en mouvement, tels des
ventilateurs, des rotors et des courroies
peuvent couper doigts et mains, ou accrocher
des vêtements amples.
1. Assurez-vous que les portes, les panneaux, les capots
et les protecteurs soient bien fermés.
2. Avant d’installer ou de connecter un système, arrêtez
le moteur.
3. Seules des personnes qualifiées doivent démonter des
protecteurs ou des capots pour faire l’entretien ou le
dépannage nécessaire.
Les moteurs produisent des gaz d’échappement nocifs.
February 22, 2006
1-9
Page 16
ARCMASTER 300 ACDC
4. Pour empêcher un démarrage accidentel pendant
l’entretien, débranchez le câble d’accumulateur à la
borne négative.
5. N’approchez pas les mains ou les cheveux de pièces
en mouvement; elles peuvent aussi accrocher des
vêtements amples et des outils.
6. Réinstallez les capots ou les protecteurs et fermez les
portes après des travaux d’entretien et avant de faire
démarrer le moteur.
AVERTISSEMENT
DES ETINCELLES PEUVENT FAIRE EXPLOSER
UN ACCUMULATEUR; L’ELECTROLYTE D’UN
ACCUMU-LATEUR PEUT BRULER LA PEAU ET
LES YEUX.
Les accumulateurs contiennent de l’électrolyte
acide et dégagent des vapeurs explosives.
1. Portez toujours un écran facial en travaillant sur un
accumu-lateur.
2. Arrêtez le moteur avant de connecter ou de
déconnecter des câbles d’accumulateur.
3. N’utilisez que des outils anti-étincelles pour travailler
sur un accumulateur.
4. N’utilisez pas une source de courant de soudage pour
charger un accumulateur ou survolter
momentanément un véhicule.
5. Utilisez la polarité correcte (+ et –) de l’accumulateur.
AVERTISSEMENT
LA VAPEUR ET LE LIQUIDE DE
REFROIDISSEMENT BRULANT SOUS
PRESSION PEUVENT BRULER LA PEAU ET
LES YEUX.
Le liquide de refroidissement d’un radiateur
peut être brûlant et sous pression.
1. N’ôtez pas le bouchon de radiateur tant que le moteur
n’est pas refroidi.
2. Mettez des gants et posez un torchon sur le bouchon
pour l’ôter.
3. Laissez la pression s’échapper avant d’ôter
complètement le bouchon.
1.05 Principales Normes de Securite
Safety in Welding and Cutting, norme ANSI Z49.1, American
Welding Society, 550 N.W. LeJeune Rd., Miami, FL 33128.
Safety and Health Standards, OSHA 29 CFR 1910, Superintendent
of Documents, U.S. Government Printing Office, Washington, D.C.
20402.
Recommended Safe Practices for the Preparation for Welding and
Cutting of Containers That Have Held Hazardous Substances,
norme AWS F4.1, American Welding Society, 550 N.W. LeJeune
Rd., Miami, FL 33128.
National Electrical Code, norme 70 NFPA, National Fire Protection
Association, Batterymarch Park, Quincy, MA 02269.
Safe Handling of Compressed Gases in Cylinders, document P-1,
Compressed Gas Association, 1235 Jefferson Davis Highway , Suite
501, Arlington, VA 22202.
Code for Safety in Welding and Cutting, norme CSA W117.2
Association canadienne de normalisation, Standards Sales, 276
Rexdale Boulevard, Rexdale, Ontario, Canada M9W 1R3.
Safe Practices for Occupation and Educational Eye and Face
Protection, norme ANSI Z87.1, American National Standards
Institute, 1430 Broadway, New York, NY 10018.
Cutting and Welding Processes, norme 51B NFPA, National Fire
Protection Association, Batterymarch Park, Quincy, MA 02269.
1-10
February 22, 2006
Page 17
ARCMASTER 300 ACDC
1.06 Limited Warranty
LIMITED WARRANTY: Thermal Arc®, Inc., A Thermadyne Company, hereafter, “Thermal Arc” warrants to customers of itsauthorized distributors
hereafter “Purchaser” that its products will be free of defects in workmanship or material. Should anyfailure to conform to this warranty appear within
the time period applicable to the Thermal Arc products as stated below, Thermal Arc shall, upon notification thereof and substantiation that the product
has been stored, installed, operated, and maintained in accordance with Thermal Arc’s specifications, instructions, recommendations and recognized
standard industry practice, and not subject to misuse, repair, neglect, alteration, or accident, correct such defects by suitable repair or replacement, at
Thermal Arc’s sole option, of any components or parts of the product determined by Thermal Arc to be defective.
THERMAL ARC MAKES NO OTHER WARRANTY, EXPRESS OR IMPLIED. THIS WARRANTY IS EXCLUSIVE AND IN LIEU OF ALL OTHERS, INCLUDING,
BUT NOT LIMITED TO ANY WARRANTY OF MERCHANTABILITY OR FITNESS FOR ANY PARTICULAR PURPOSE.
LIMITATION OF LIABILITY: THERMAL ARC SHALL NOT UNDER ANY CIRCUMSTANCES BE LIABLE FOR SPECIAL, INDIRECT OR CONSEQUENTIAL
DAMAGES, SUCH AS, BUT NOT LIMITED TO, LOST PROFITS AND BUSINESS INTERRUPTION. The remedies of the Purchaser set forth herein are
exclusive and the liability of Thermal Arc with respect to any contract, or anything done in connection therewith such as the performance or breach
thereof, or from the manufacture, sale, delivery, resale, or use of any goods covered by or furnished by Thermal Arc whether arising out of contract,
negligence, strict tort, or under any warranty, or otherwise, shall not, except as expressly provided herein, exceed the price of the goods upon which
such liability is based. No employee, agent, or representative of Thermal Arc is authorized to change this warranty in any way or grant any other
warranty.
PURCHASER’S RIGHTS UNDER THIS WARRANTY ARE VOID IF REPLACEMENT PARTS OR ACCESSORIES ARE USED WHICH IN THERMAL ARC’S SOLE
JUDGEMENT MAY IMPAIR THE SAFETY OR PERFORMANCE OF ANY THERMAL ARC PRODUCT. PURCHASER’S RIGHTS UNDER THIS WARRANTY ARE
VOID IF THE PRODUCT IS SOLD TO PURCHASER BY NON-AUTHORIZED PERSONS.
The warranty is effective for the time stated below beginning on the date that the authorized distributor delivers the products to the Purchaser.
Notwithstanding the foregoing, in no event shall the warranty period extend more than the time stated plus one year from the date Thermal Arc
delivered the product to the authorized distributor.
POWER SUPPLIES
MAIN POWER MAGNETICS (STATIC & ROTATING) 3 YEARS 3 YEAR
ORIGINAL MAIN POWER RECTIFIER 3 YEARS 3 YEAR
CONTROL PC BOARD 3 YEARS 3 YEAR
ALL OTHER CIRCUITS AND COMPONENTS INCLUDING BUT
NOT LIMITED TO: CONTACTORS, RELAYS, SOLENOIDS, PUMPS,
POWER SWITCHING SEMI-CONDUCTORS.
ENGINES: ENGINES ARE NOT WARRANTED BY THERMAL ARC,
ALTHOUGH MOST ARE WARRANTED BY THE ENGINE
MANUFACTURER. SEE THE ENGINE MANUFACTURE'S 1 YEAR 1 YEAR
WARR ANTY FOR DETAILS.
CONSOLES, CONTROL EQUIPMENT, HEAT EXCHANGES
ACCESSORY EQUIPMENT
NOTE: Dragster 85® excluded from this policy. Refer to Dragster 85 warranty in Dragster 85 Owner’s Manual.
Warranty repairs or replacement claims under this limited warranty must be submitted to Thermal Arc by an authorized Thermal Arc repair facility
within thirty (30) days of purchaser’s notice of any Warranty Claim. No transportation costs of any kind will be paid under this warranty. Transportation
charges to send products to an authorized warranty repair facility shall be the responsibility of the Purchaser. All returned goods shall be at the
Purchaser’s risk and expense. This warranty supersedes all previous Thermal Arc warranties. Thermal Arc® is a Registered Trademark of Thermadyne
Industries Inc.
September 27, 2004
ALL OTHER
POWER SUPPLIES
1 YEAR 1 YEAR
LABOR
February 22, 2006
1-11
Page 18
ARCMASTER 300 ACDC
1-12
February 22, 2006
Page 19
ARCMASTER 300 ACDC
!
SECTION 2:
INTRODUCTION
2.01 How To Use This Manual
This Owner’s Manual applies to just specification or part
numbers listed on page i.
To ensure safe operation, read the entire manual, including
the chapter on safety instructions and warnings.
Throughout this manual, the words WARNING,
CAUTION, and NOTE may appear. Pay particular attention
to the information provided under these headings. These
special annotations are easily recognized as
follows:
WARNING
A WARNING gives information regarding
possible personal injury.
2.02 Equipment Identification
The unit’s identification number (specification or part
number), model, and serial number usually appear on a
nameplate attached to the control panel. In some cases,
the nameplate may be attached to the rear panel.
Equipment which does not have a control panel such as
gun and cable assemblies is identified only by the
specification or part number printed on the shipping
container. Record these numbers on the bottom of page
1 for future reference.
2.03 Receipt Of Equipment
When you receive the equipment, check it against the
invoice to make sure it is complete and inspect the
equipment for possible damage due to shipping. If there
is any damage, notify the carrier immediately to file a
claim. Furnish complete information concerning damage
claims or shipping errors to the location in your area
listed in the inside back cover of this manual.
Include all equipment identification numbers as described
above along with a full description of the parts in error.
CAUTION
A CAUTION refers to possible equipment
damage.
NOTE
A NOTE offers helpful information concerning
certain operating procedures.
Additional copies of this manual may be purchased by
contacting Thermal Arc at the address and phone number
given in the next section. Include the Owner’s Manual
number and equipment identification numbers.
Electronic copies of this manual can also be downloaded
at no charge in Acrobat PDF format by going to the
Thermal Arc web site listed below and clicking on the
Literature Library link:
http://www.thermalarc.com
Move the equipment to the installation site before uncrating the unit. Use care to avoid damaging the
equipment when using bars, hammers, etc., to un-crate
the unit.
February 22, 2006
2-1
Page 20
ARCMASTER 300 ACDC
2.04 Symbol Chart
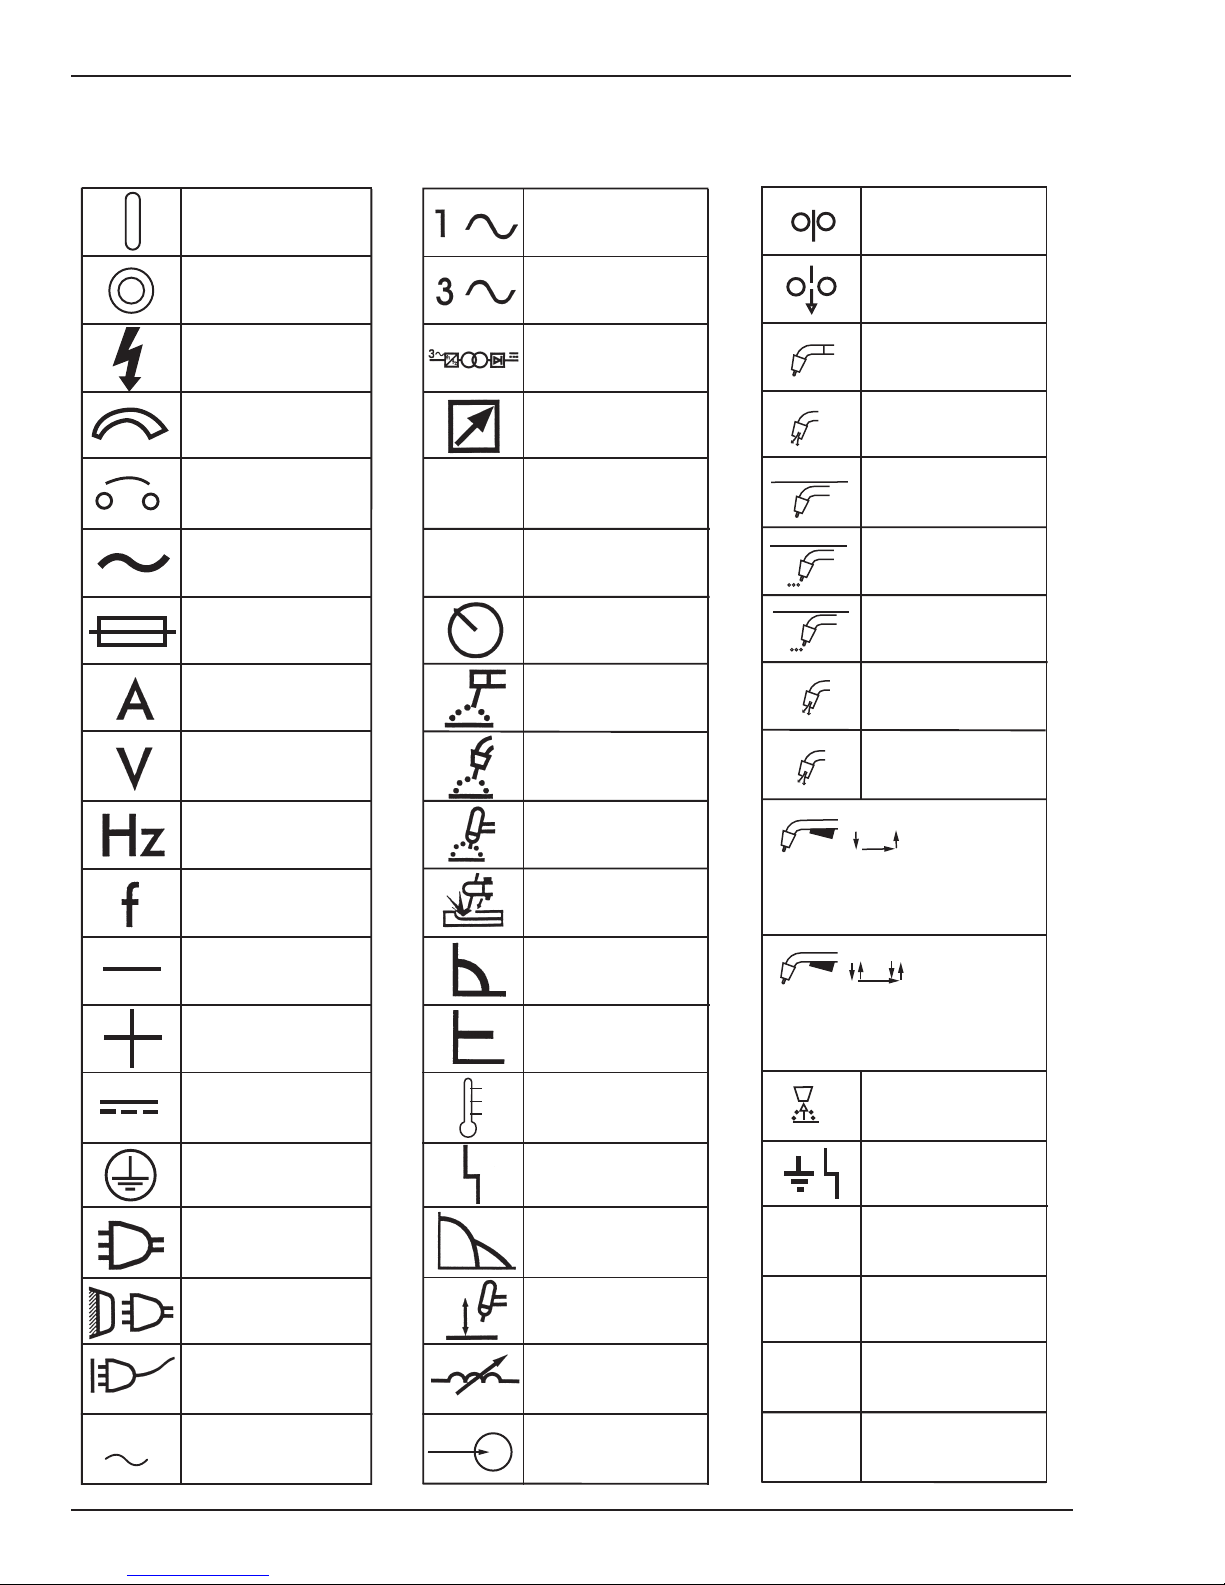
Note that only some of these symbols will appear on your model.
On
Off
Dangerous Voltage
Increase/Decrease
Circuit Breaker
AC Auxiliary Power
Fuse
Amperage
Voltage
X
%
Single Phase
Three Phase
Three Phase Static
Frequency ConverterTransformer-Rectifier
Remote
Duty Cycle
Percentage
Panel/Local
Shielded Metal
Arc Welding (SMAW)
Gas Metal Arc
Welding (GMAW)
Wire Feed Function
Wire Feed Towards
Workpiece With
t1
Output Voltage Off.
Welding Gun
Purging Of Gas
Continuous Weld
Mode
Spot Weld Mode
Spot Time
t
Preflow Time
Postflow Time
t2
Hertz (cycles/sec)
Frequency
Negative
Positive
Direct Current (DC)
Protective Earth
(Ground)
Line
Line Connection
Auxiliary Power
Gas Tungsten Arc
Welding (GTAW)
Air Carbon Arc
Cutting (CAC-A)
Constant Current
Constant Voltage
Or Constant Potential
High Temperature
Fault Indication
Arc Force
Touch Start (GTAW)
Variable Inductance
2 Step Trigger
Operation
Press to initiate wirefeed and
welding, release to stop.
4 Step Trigger
Operation
Press and hold for preflow, release
to start arc. Press to stop arc, and
hold for preflow.
Burnback Time
t
Disturbance In
Ground System
IPM
MPM
Inches Per Minute
Meters Per Minute
115V 15A
2-2
Receptacle RatingAuxiliary Power
Voltage Input
V
Art # A-04130
February 22, 2006
Page 21
2.05 Description
ARCMASTER 300 ACDC
The Thermal Arc™ Model 300 ACDC is a self contained
single-phase AC/DC arc welding power source with
Constant Current (CC) output characteristics. This unit
is equipped with a Digital Volt/Amperage Meter, gas
control valve, built in Sloper and Pulser, lift arc starter,
and high-frequency arc starter for use with Gas Tungsten
Arc Welding (GTAW), Gas Tungsten Arc Welding-Pulsed
(GTAW-P) Gas Tungsten Arc Welding-Sloped (GTAW-S),
and Shielded Metal Arc Welding (SMAW) processes. The
power source is totally enclosed in an impact resistant,
flame retardant and non-conductive plastic case.
NOTE
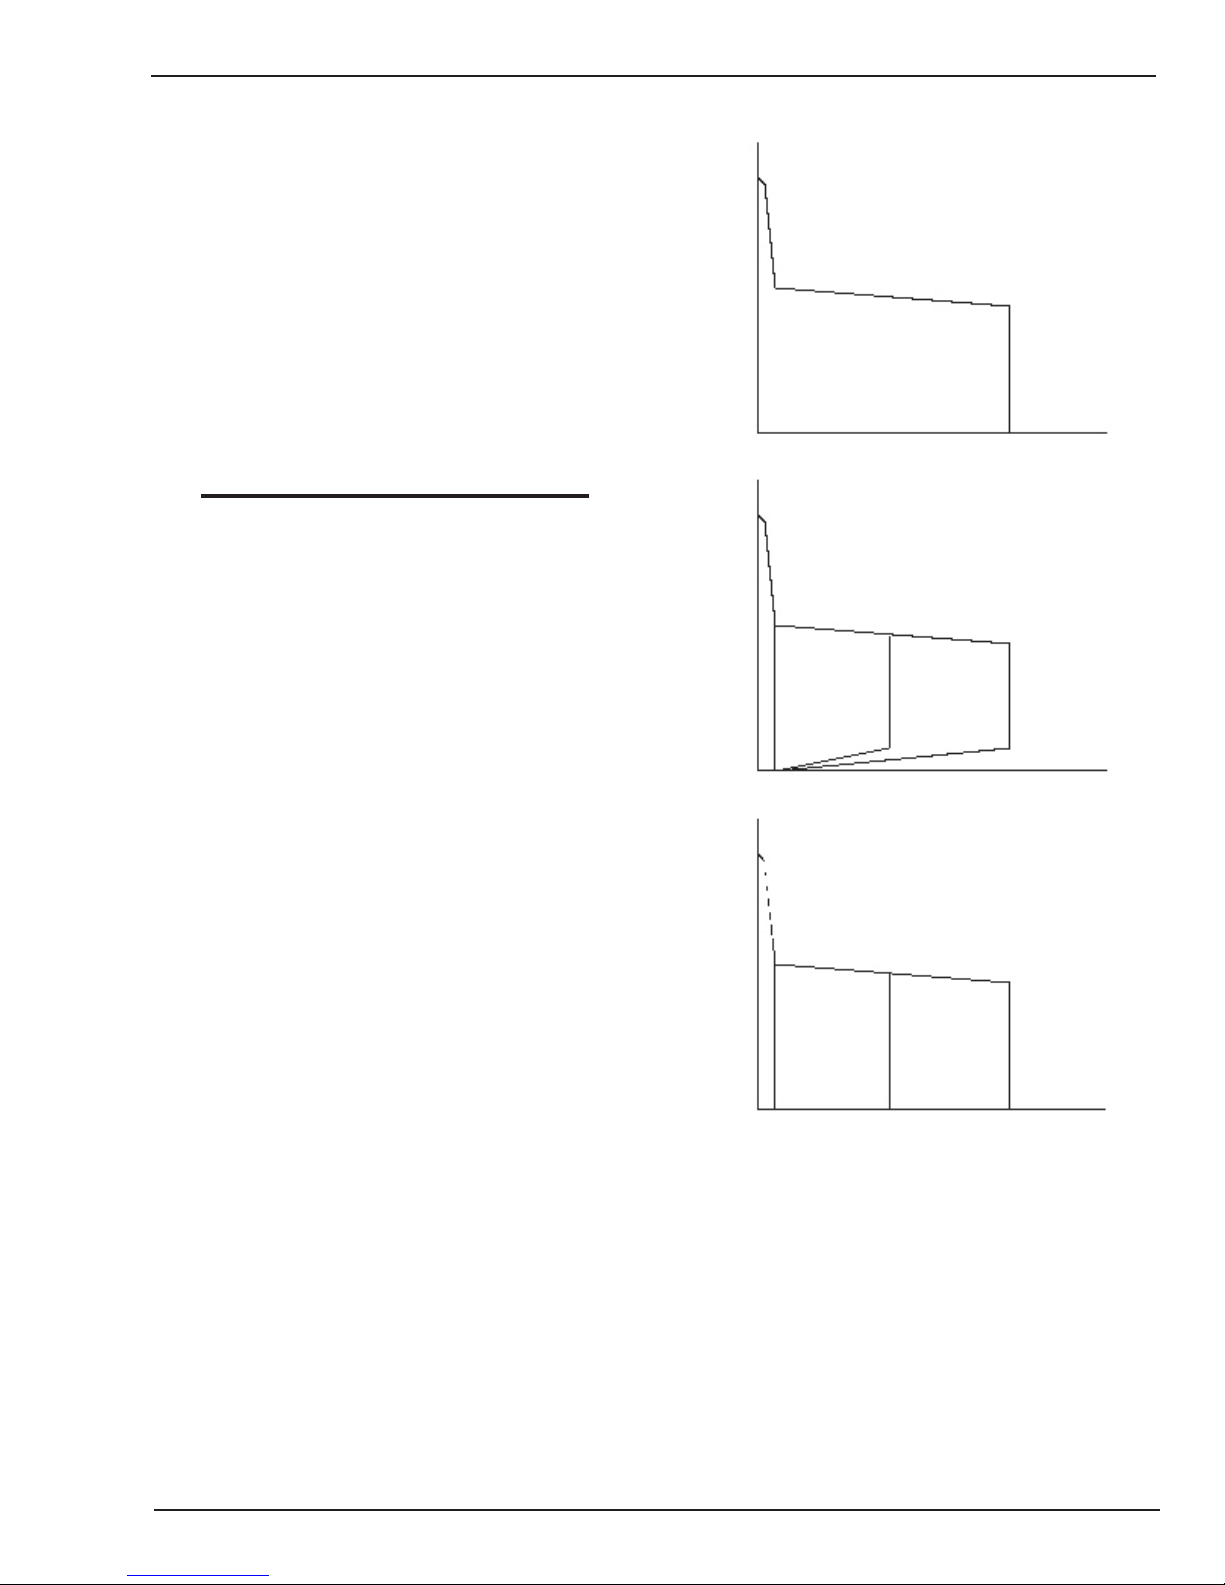
Volt-Ampere curves show the maximum
Voltage and Amperage output capabilities of
the welding power source. Curves of other
settings will fall between the curves shown.
(V)
CCV
5A 160A (A)
STICK Process
(V)
CCV
Art # A-04980
10V
25A 185A
(A)
LIFT TIG Process
(V)
CCV
5A
185A
(A)
HF TIG Process
Figure 2-1: Model 300 ACDC Volt-Ampere curve
February 22, 2006
2-3
Page 22
ARCMASTER 300 ACDC
2.06 Functional Block Diagrams
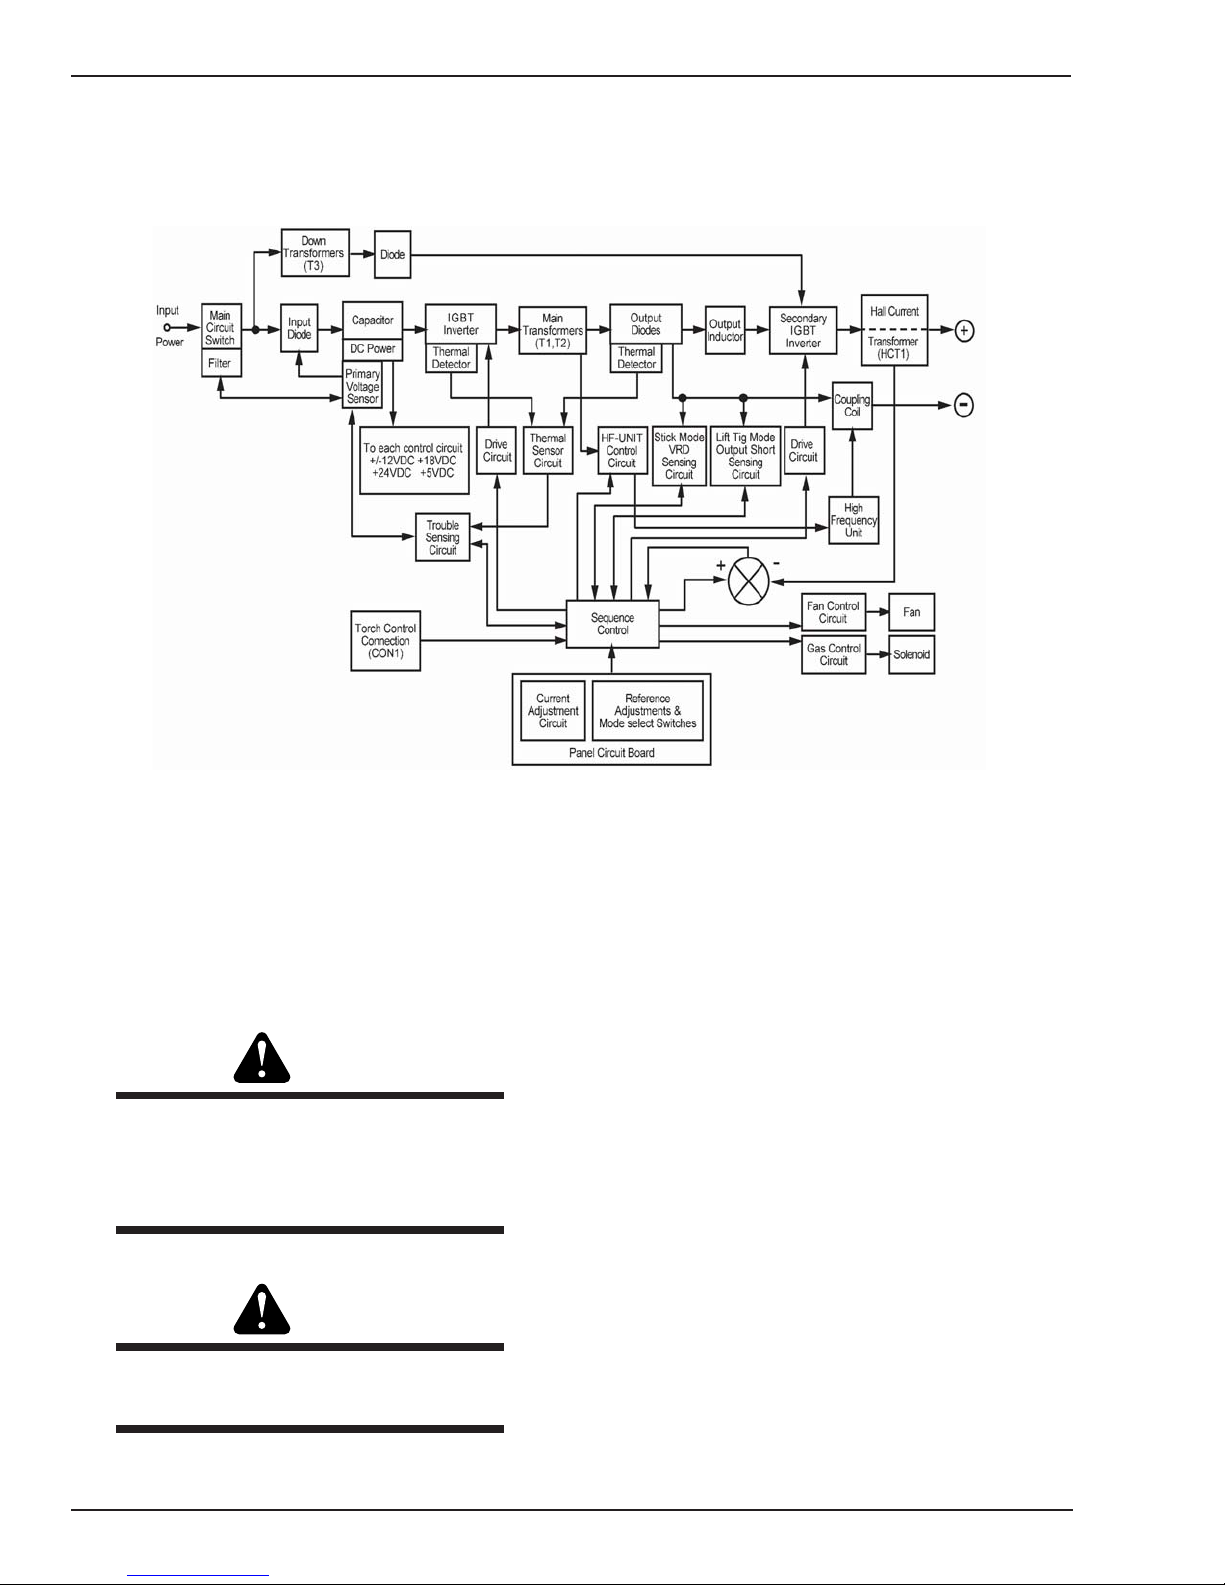
Figure 2-2 illustrates the functional block diagram of the 300 ACDC-power supply.
Art # A-04981
Figure 2-2: 300 ACDC Model Functional Block Diagram
2.07 Transporting Methods
These units are equipped with a handle for carrying
purposes.
WARNING
ELECTRIC SHOCK can kill. DO NOT TOUCH
live electrical parts. Disconnect input power
conductors from de-energized supply line
before moving the welding power source.
WARNING
FALLING EQUIPMENT can cause serious
personal injury and equipment damage.
• Lift unit with handle on top of case.
• Use handcart or similar device of adequate capacity.
• If using a fork lift vehicle, place and secure unit on a
proper skid before transporting.
2-4
February 22, 2006
Page 23
ARCMASTER 300 ACDC
SECTION 3:
INSTALLATION
3.01 Environment
The ArcMaster 300 ACDC is designed for use in adverse
environments.
Examples of environments with increased adverse
conditions are:
a. In locations in which freedom of movement is
restricted, so that the operator is forced to perform the
work in a cramped (kneeling, sitting or lying) position
with physical contact with conductive parts;
b. In locations which are fully or partially limited by
conductive elements, and in which there is a high risk of
unavoidable or accidental contact by the operator;
c. In wet or damp hot locations where humidity or
perspiration considerably reduces the skin resistance of
the human body and the insulation properties of
accessories.
3.03 Electrical Input Connections
WARNING
ELECTRIC SHOCK can kill; SIGNIFICANT DC
VOLTAGE is present after removal of input
power.
DO NOT TOUCH live electrical parts.
SHUT DOWN welding power source, disconnect input
power employing lockout/tagging procedures. Lockout/
tagging procedures consist of padlocking line disconnect
switch in open position, removing fuses from fuse box,
or shutting off and red-tagging circuit breaker or other
disconnecting device.
Environments with adverse conditions do not include
places where electrically conductive parts, in the near
vicinity of the operator, which can cause increased hazard,
have been insulated.
3.02 Location
Be sure to locate the welder according to the following
guidelines:
·
In areas, free from moisture and dust.
·
Ambient temperature between 0 degrees C to 40
degrees C.
·
In areas, free from oil, steam and corrosive gases.
·
In areas, not subjected to abnormal vibration or
shock.
·
In areas, not exposed to direct sunlight or rain.
·
Place at a distance of 12" (304.79mm) or more from
walls or similar boundaries that could restrict natural
airflow for cooling.
WARNING
Thermal Arc advises that this equipment be
electrically connected by a qualified electrician.
Februrary 22, 2006
3-1
Page 24
ARCMASTER 300 ACDC
3.04 Electrical Input Requirements
Operate the welding power source from a single-phase
50/60 Hz, AC power supply. The input voltage must match
one of the electrical input voltages shown on the input
data label on the unit nameplate. Contact the local electric
utility for information about the type of electrical service
available, how proper connections should be made, and
any inspection required.
The line disconnect switch provides a safe and convenient
means to completely remove all electrical power from
the welding power supply whenever necessary to inspect
or service the unit.
NOTE
These units are equipped with a two-conductor
with earth power cable that is connected at
the welding power source end for single-phase
electrical input power.
Input Voltage Fuse Size
208V 45 Amps
230V 40 Amps
Do not connect an input (WHITE or BLACK) conductor to
the ground terminal.
Do not connect the ground (GREEN) conductor to an input
line terminal.
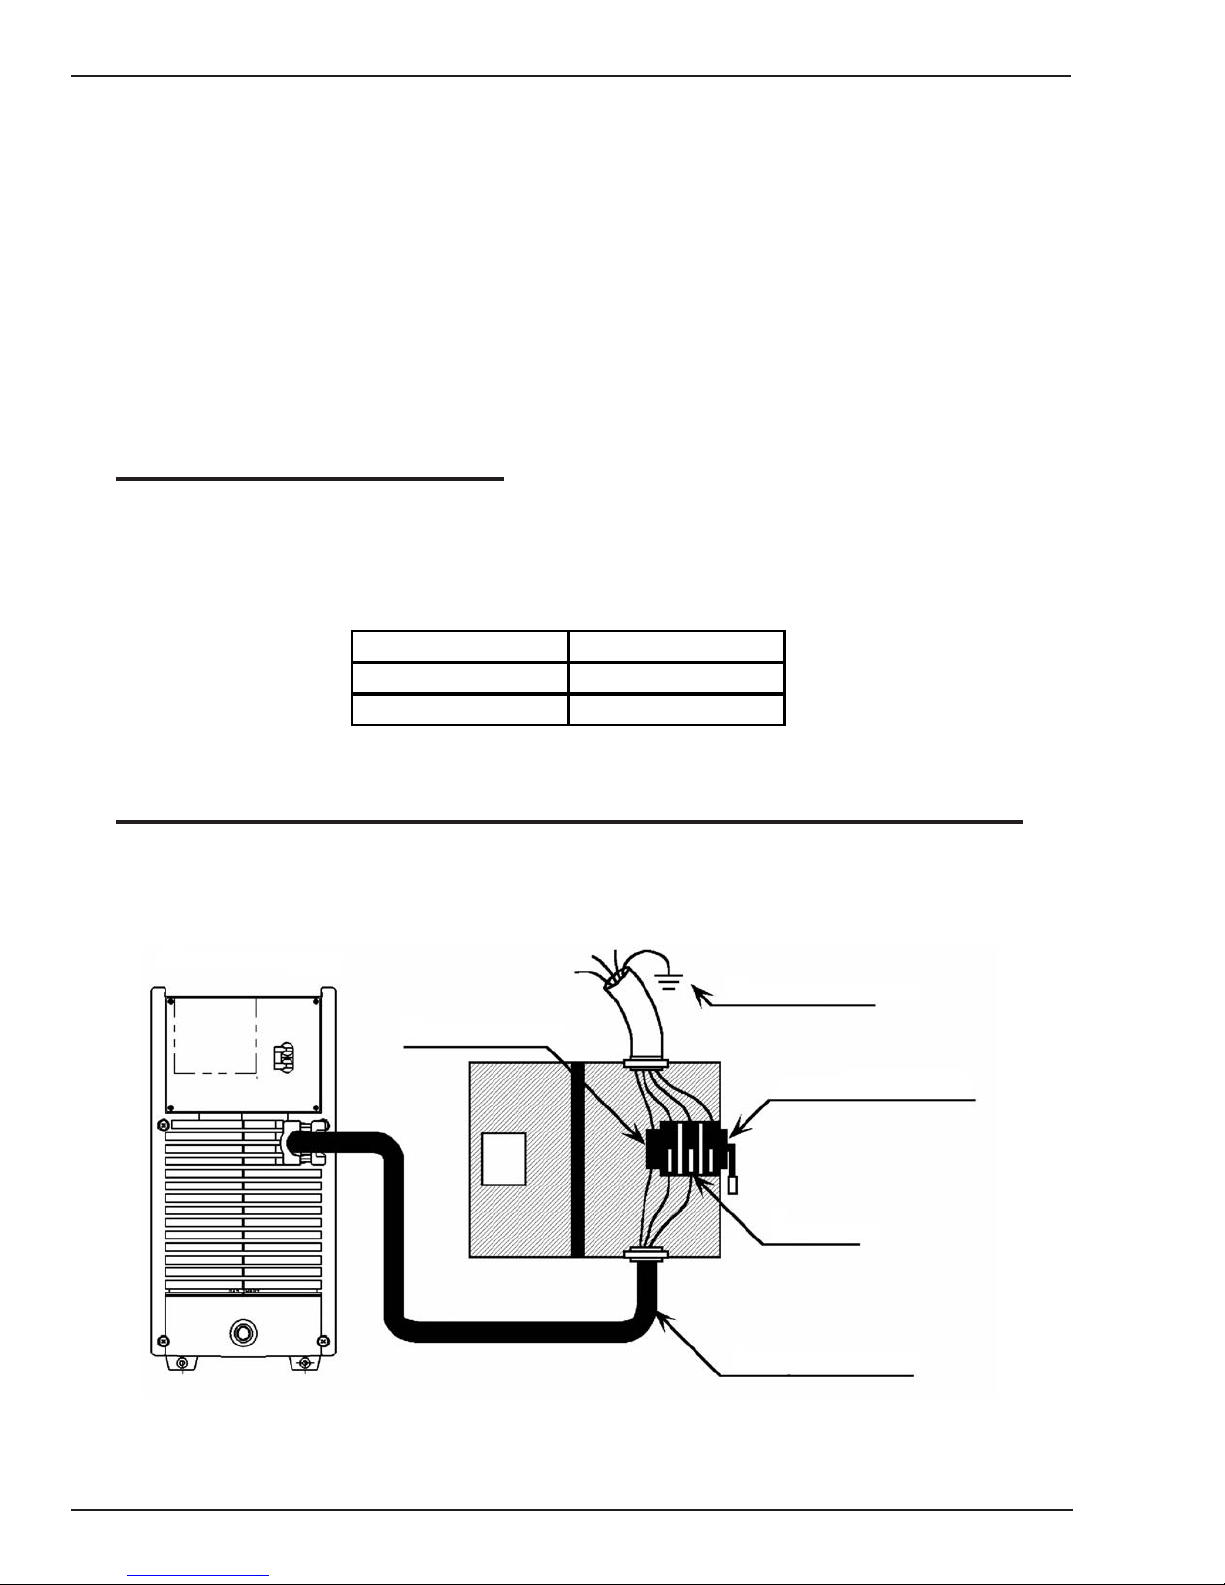
Refer to Figure 3-1 and:
1. Connect end of ground (GREEN) conductor to a
suitable ground. Use a grounding method that complies
with all applicable electrical codes.
2. Connect ends of line 1 (BLACK) and line 2 (WHITE)
input conductors to a de-energized line disconnect switch.
3. Use Table 3-1 and Table 3-2 as a guide to select line
fuses for the disconnect switch.
Table 3-1: Electrical Input Connections
NOTE
Fuse size is based on not more than 200 percent of the rated input amperage of the welding power source
(Based on Article 630, National Electrical Code).
Welding Power Supply
Art # A-04982
Ground Conductor
Ground Terminal
Line Disconnect Switch
Line Fuse
Figure 3-1: Electrical Input Connections
3-2
Primary Power Cable
February 22, 2006
Page 25
ARCMASTER 300 ACDC
3.05 Input Power
Each unit incorporates an INRUSH circuit and input voltage sensing circuit. When the MAIN CIRCUIT SWITCH is
turned on, the inrush circuit provides a pre-charging of the input capacitors. SCR’s in the Power Control Assembly
(PCA) will turn on after the input capacitors have charged to full operating voltage (after approximately 5 seconds).
NOTE
Note the available input power. Damage to the PCA could occur if 460VAC or higher is applied.
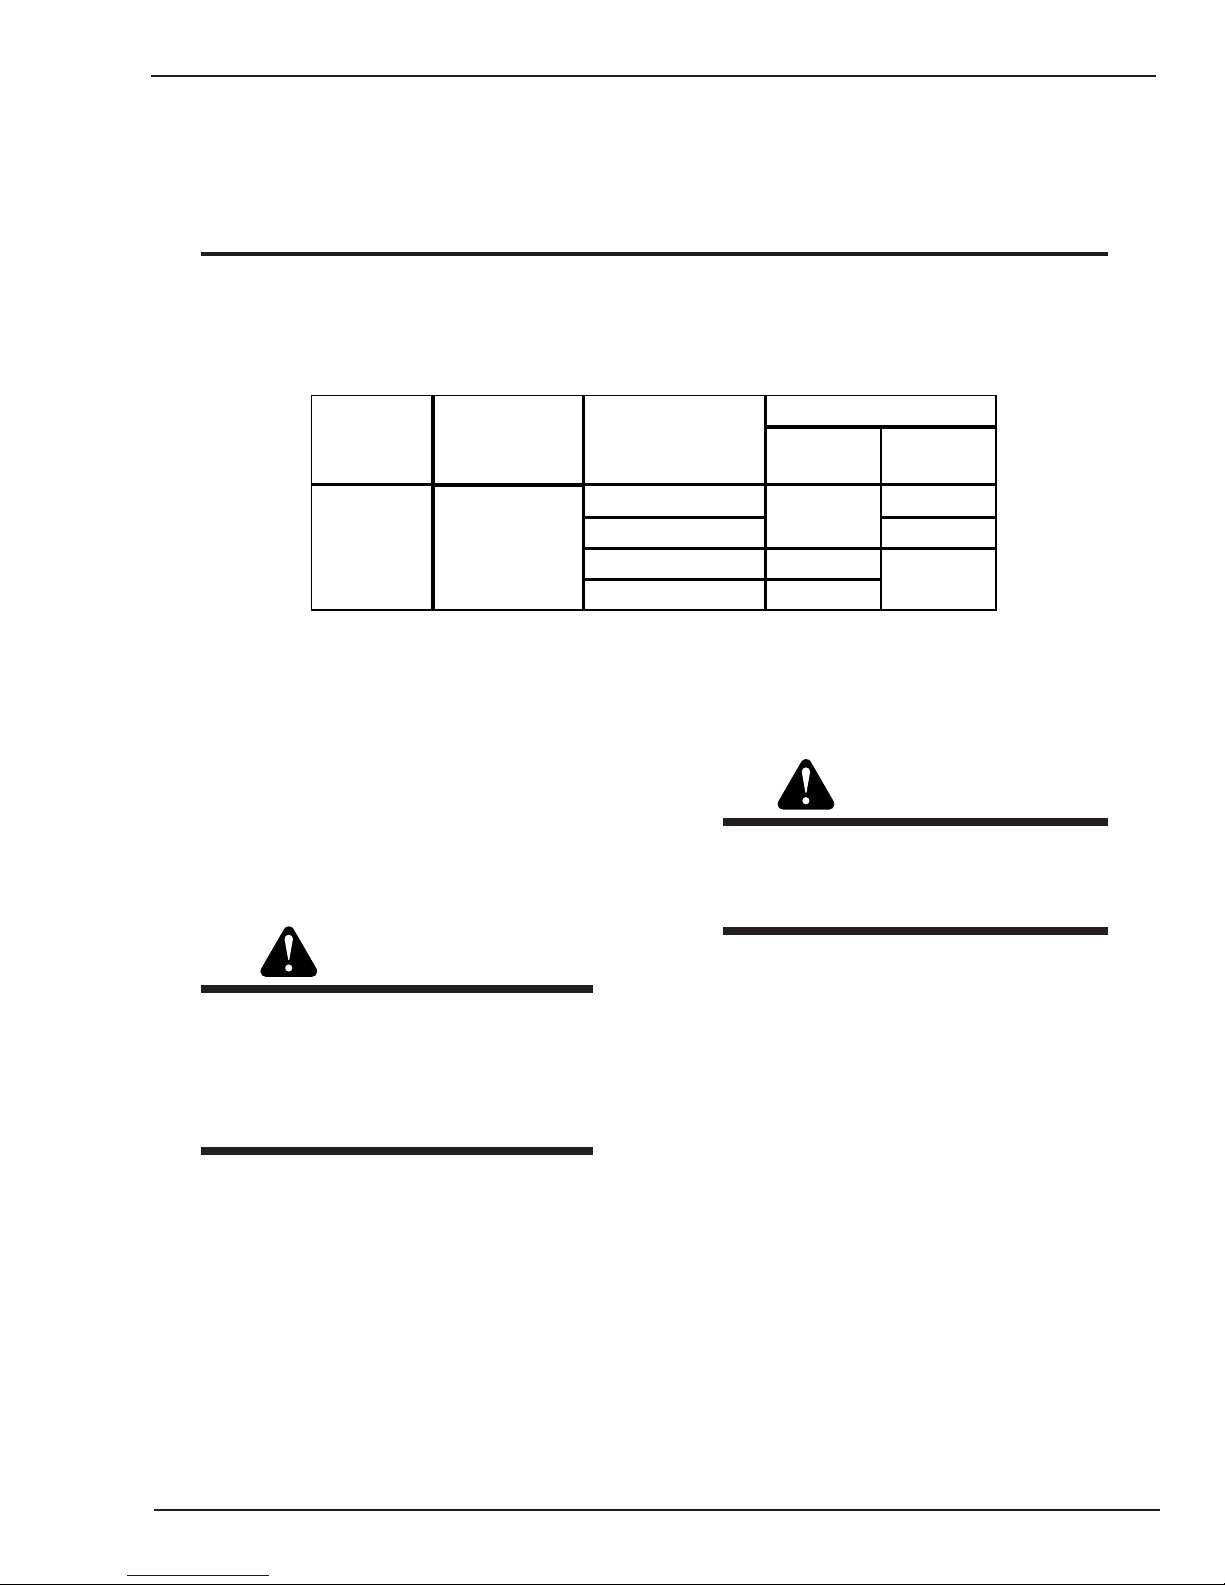
The following 208/230V Primary Current recommendations are required to obtain the maximum welding current and
duty cycle from this welding equipment:
Primary Supply
Model
ArcMaster
300ACDC
Table 3-2 208/230V Primary Current Circuit sizes to achieve maximum current
Lead Size
(Factory Fitted)
12/3 AWG
minimum
Minimum Primary
Current Circuit Size
3.06 High Frequency Introduction
The importance of correct installation of high frequency
welding equipment cannot be over-emphasized.
Interference due to high frequency initiated or stabilized
arc is almost invariably traced to improper installation.
The following information is intended as a guide for
personnel installing high frequency welding machines.
WARNING: EXPLOSIVES
(Vin/Amps)
230/29
208/32
230/38 208/40 -
185 @ 30%
It is also possible that operation close to
computer installations may cause computer
malfunction.
Current & Duty Cycle
TIG STICK
160 @ 40%
WARNING: COMPUTERS
The high frequency section of this machine has
an output similar to a radio transmitter. The
machine should NOT be used in the vicinity of
blasting operations due to the danger of
premature firing.
Februrary 22, 2006
3-3
Page 26
ARCMASTER 300 ACDC
3.07 High Frequency Interference
Interference may be transmitted by a high frequency
initiated or stabilized arc welding machine in the following
ways:
1. Direct Radiation: Radiation from the machine can
occur if the case is metal and is not properly grounded.
It can occur through apertures such as open access
panels. The shielding of the high frequency unit in
the Power Source will prevent direct radiation if the
equipment is properly grounded.
2. Transmission via the Supply Lead: Without adequate
shielding and filtering, high frequency energy may be
fed to the wiring within the installation (mains) by
direct coupling. The energy is then transmitted by
both radiation and conduction. Adequate shielding
and filtering is provided in the Power Source.
3. Radiation from Welding Leads: Radiated interference
from welding leads, although pronounced in the
vicinity of the leads, diminishes rapidly with distance.
Keeping leads as short as possible will minimize this
type of interference. Looping and suspending of leads
should be avoided where possible.
4. Re-radiation from Unearthed Metallic Objects:
A major factor contributing to interference is reradiation from unearthed metallic objects close to the
welding leads. Effective grounding of such objects
will prevent re-radiation in most cases.
3.08 Duty Cycle
The duty cycle of a welding power source is the percentage
of a ten (10) minute period that it can be operated at a
given output without causing overheating and damage to
the unit. If the welding amperes decrease, the duty cycle
increases. If the welding amperes are increased beyond
the rated output, the duty cycle will decrease.
WARNING
Exceeding the duty cycle ratings will cause the
thermal overload protection circuit to become
energized and shut down the output until the
unit has cooled to normal operating
temperature.
CAUTION
Continually exceeding the duty cycle ratings
can cause damage to the welding power
source and will void the manufactures warranty.
NOTE
Due to variations that can occur in
manufactured products, claimed performance,
voltages, ratings, all capacities,
measurements, dimensions and weights
quoted are approximate only. Achievable
capacities and ratings in use and operation will
depend upon correct installation, use,
applications, maintenance and service.
3-4
February 22, 2006
Page 27
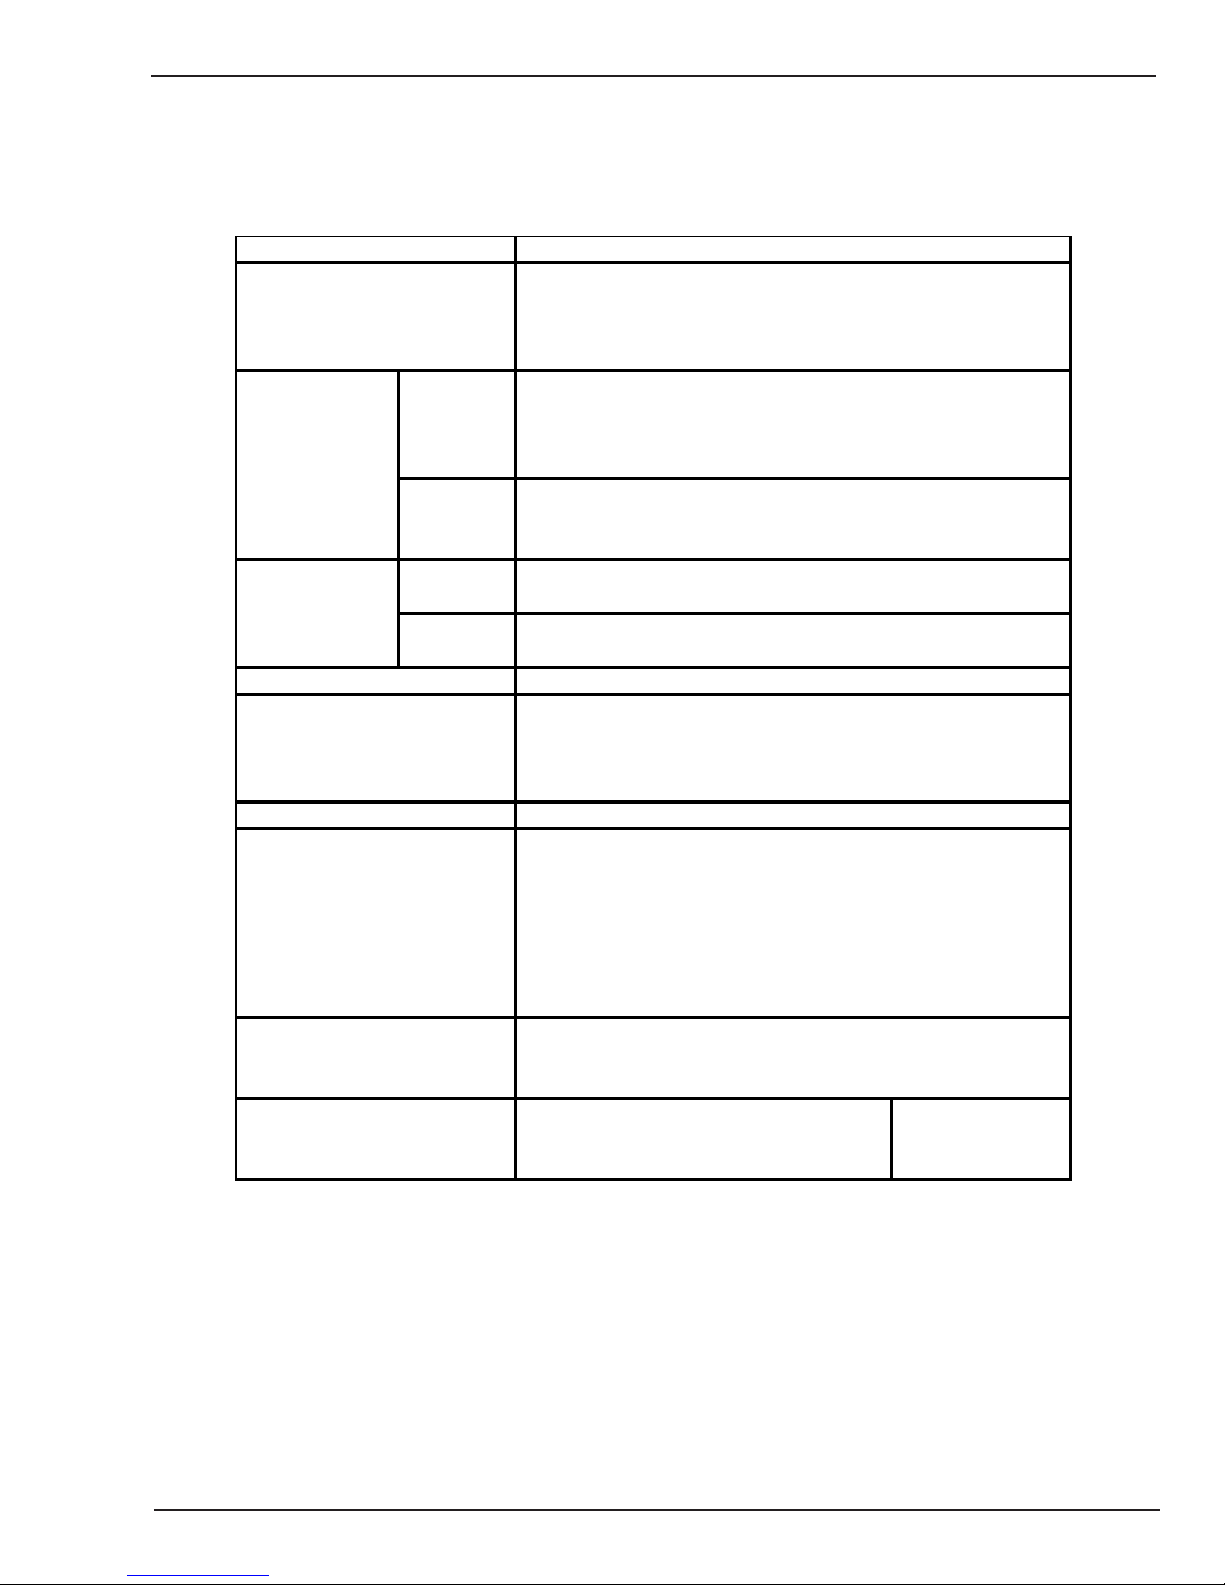
3.09 Specifications
p
p
y Cy
(DC)
g
)
g
V
g
g
(
)
)
)
g
p
g
p
p
y Cy
A
A
V
W
p
A
W
Parameter 300ACDC
Rated Out
Am
eres
Volts
Dut
Duty Cycle TIG 185A / 17.4V @ 30%
Output Current TIG 5 – 185
Range STICK 5 – 160 (DC
Open Circuit Voltage69
Dimensions
Width
Hei
ht
Len
Weight 41.8 lb. 19 k
Output @ Rated Load
Rated In
Out
Out
Dut
KV
K
Out
KV
K
Input Volts Single Phase
ut
cle
th
ut VoltageSin
ut Amperes
ut Volts
cle
ut @ No Load
208V
230V
185
17.4
25%
160A / 16V @ 40%
130A / 15V @ 60%
100A / 14V @ 100%
STICK 160A / 26V @ 40%
130A / 25V @ 60%
100A / 25V @ 100%
5 – 185 (AC) @ 60Hz, 50% Cleanin
5 – 160 (AC) @ 60Hz, 50% Cleanin
7.08”
180mm
14.7” (360mm
16.54” (420mm
0.5
0.13
Amperage Draw @ Rated Load No Load Amps
ARCMASTER 300 ACDC
le phase 230VAC
160
26
40%
8.7
5.2
40 2.2
38 1.6
Februrary 22, 2006
Table 3-3: Parameter Specifications
3-5
Page 28
ARCMASTER 300 ACDC
3-6
February 22, 2006
Page 29
OPERATOR CONTROLS
4.01 ArcMaster 300 ACDC Controls
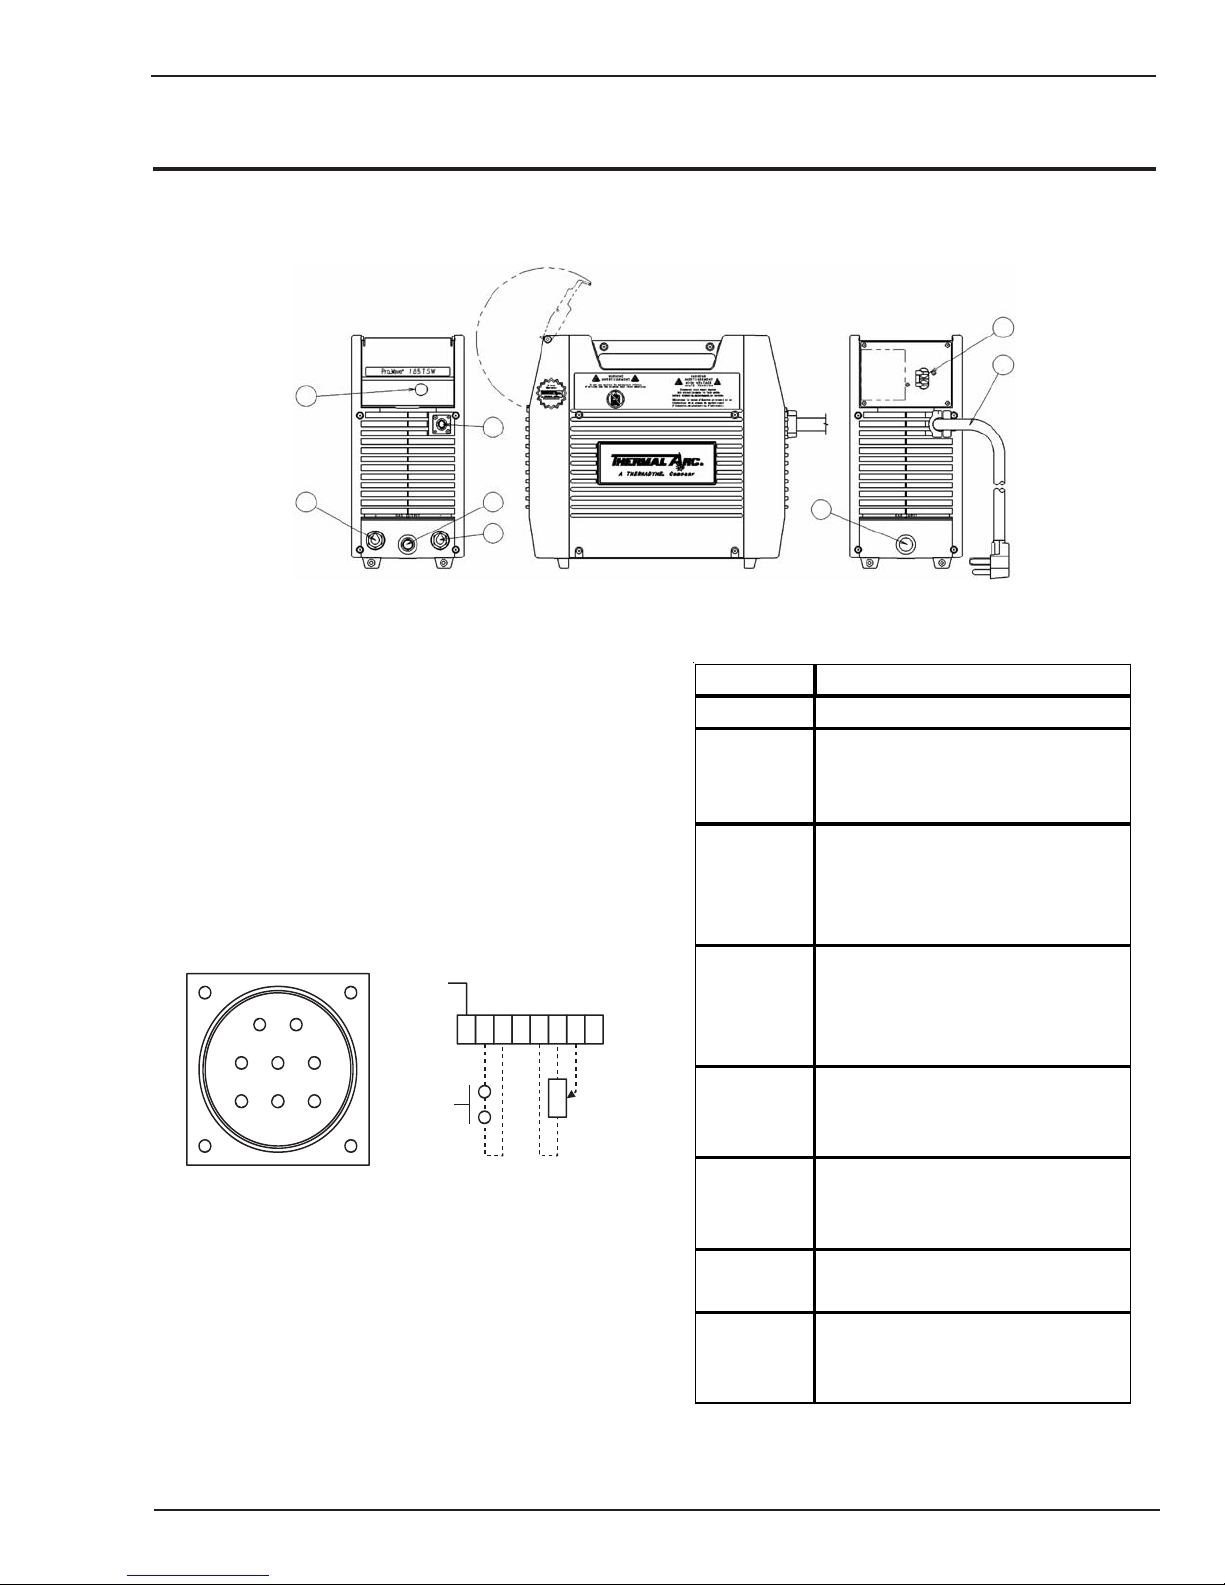
1
2
ARCMASTER 300 ACDC
SECTION 4:
Art # A-04983
6
7
3
5
4
Figure 4-1: ArcMaster 300 ACDC Power Source
1. Control Knob: This control sets the selected weld
parameter, rotating it clockwise increases the parameter
that is indicated on the digital meter. Pushing the knob
inward displays the actual welding voltage.
2 . Remote Control Socket: The 8 pin Remote Control
Socket is used to connect remote current control
devices to the welding Power Source. To make
connections, align keyway, insert plug, and rotate
threaded collar fully clockwise.
Art # A-04984
5k Ohms
21
543
678
GND
12345678
Figure 4-2: 8-Socket Receptacle
8
Socket Pin Function
1 Earth (Ground)
2
Torch Switch Input (24V) to
(connect pins 2 & 3 to turn on
welding current)
3 Torch Switch Input (0V) to
energize weld current (connect
pins 2 & 3 to turn on welding
current)
4 Connectpin4topin8toinstruct
machine that a remote current
control device is connected (12V
DC supply)
5 5k ohm (maximum) connection
to 5k ohm remote control
potentiometer
6 Zero ohm (minimum) connection
to 5k ohm remote control
potentiometer
7 Wiper arm connection to 5k ohm
remote control potentiometer
8 Connectpin4topin8toinstruct
machine that a remote current
control device is connected (0V)
February 22, 2006
Table 4-1: Socket Pin Functions
4-1
Page 30
ARCMASTER 300 ACDC
3. Positive Terminal: Welding current flows from the
Power Source via heavy duty Dinse type terminal. It
is essential, however, that the male plug is inserted
and turned securely to achieve a sound electrical
connection.
4. Negative Terminal: Welding current flows from the
Power Source via heavy duty Dinse type terminal. It
is essential, however, that the male plug is inserted
and turned securely to achieve a sound electrical
connection.
CAUTION
Loose welding terminal connections can cause
overheating and result in the male plug being
fused in the bayonet terminal.
5. Gas Outlet: The Gas Outlet is a 5/8 18 UNF female gas
fitting.
6. ON/OFF Switch: This switch connects the Primary
supply voltage to the inverter when in the ON position.
This enables the Power Supply.
WARNING
When the welder is connected to the Primary
supply voltage, the internal electrical
components maybe at 240V potential with
respect to earth.
7. Input Cable: The input cable connects the Primary
supply voltage to the equipment.
8 . Gas Inlet: The Gas Inlet is a 5/8 18 UNF female gas
fitting.
4-2
February 22, 2006
Page 31
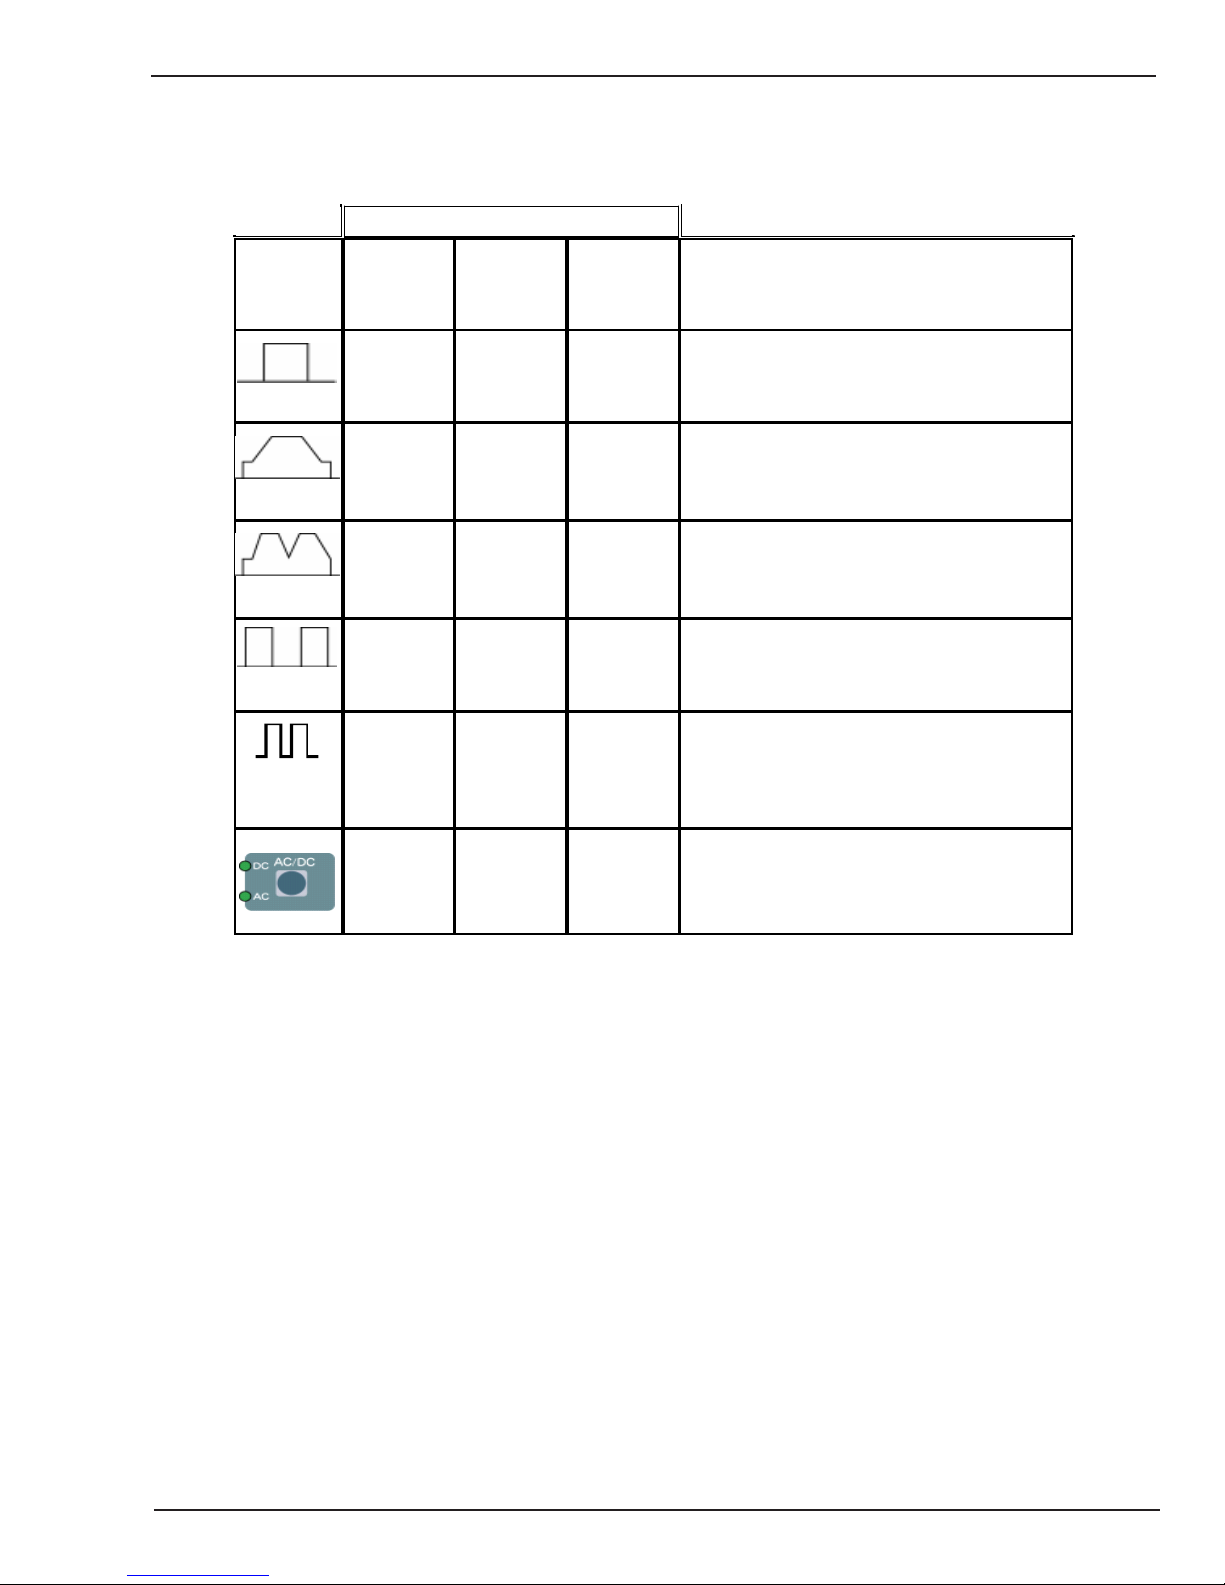
4.02 Weld Process Selection for ArcMaster 300 ACDC
Weld Mode
Weld
Process
Selection
LIFT TIGSTICK HF TIG
ARCMASTER 300 ACDC
Description
STD
SLOPE
REPEAT
SPOT
PULSE
ON/OFF
Yes Yes Yes
No Yes Yes
No Yes Yes
No Yes No
No Yes Yes
Yes Yes Yes
2T operation in TIG Modes using remote
devices to control contactor & current
4T operation in TIG Modes with crater fill
using a remote contactor device to
control sequence.
4T operation in TIG Modes with repeat
operation and crater fill using a remote
contactor device.
2T operation spot welding in HF TIG using
a remote contactor device.
Pulse operation in TIG Modes
Selects AC or DC weld current
Table 4-2: Weld Process selection versus Weld Mode for ArcMaster 300 ACDC
February 22, 2006
4-3
Page 32
ARCMASTER 300 ACDC
4.03 Weld Parameter Descriptions for ArcMaster 300 ACDC
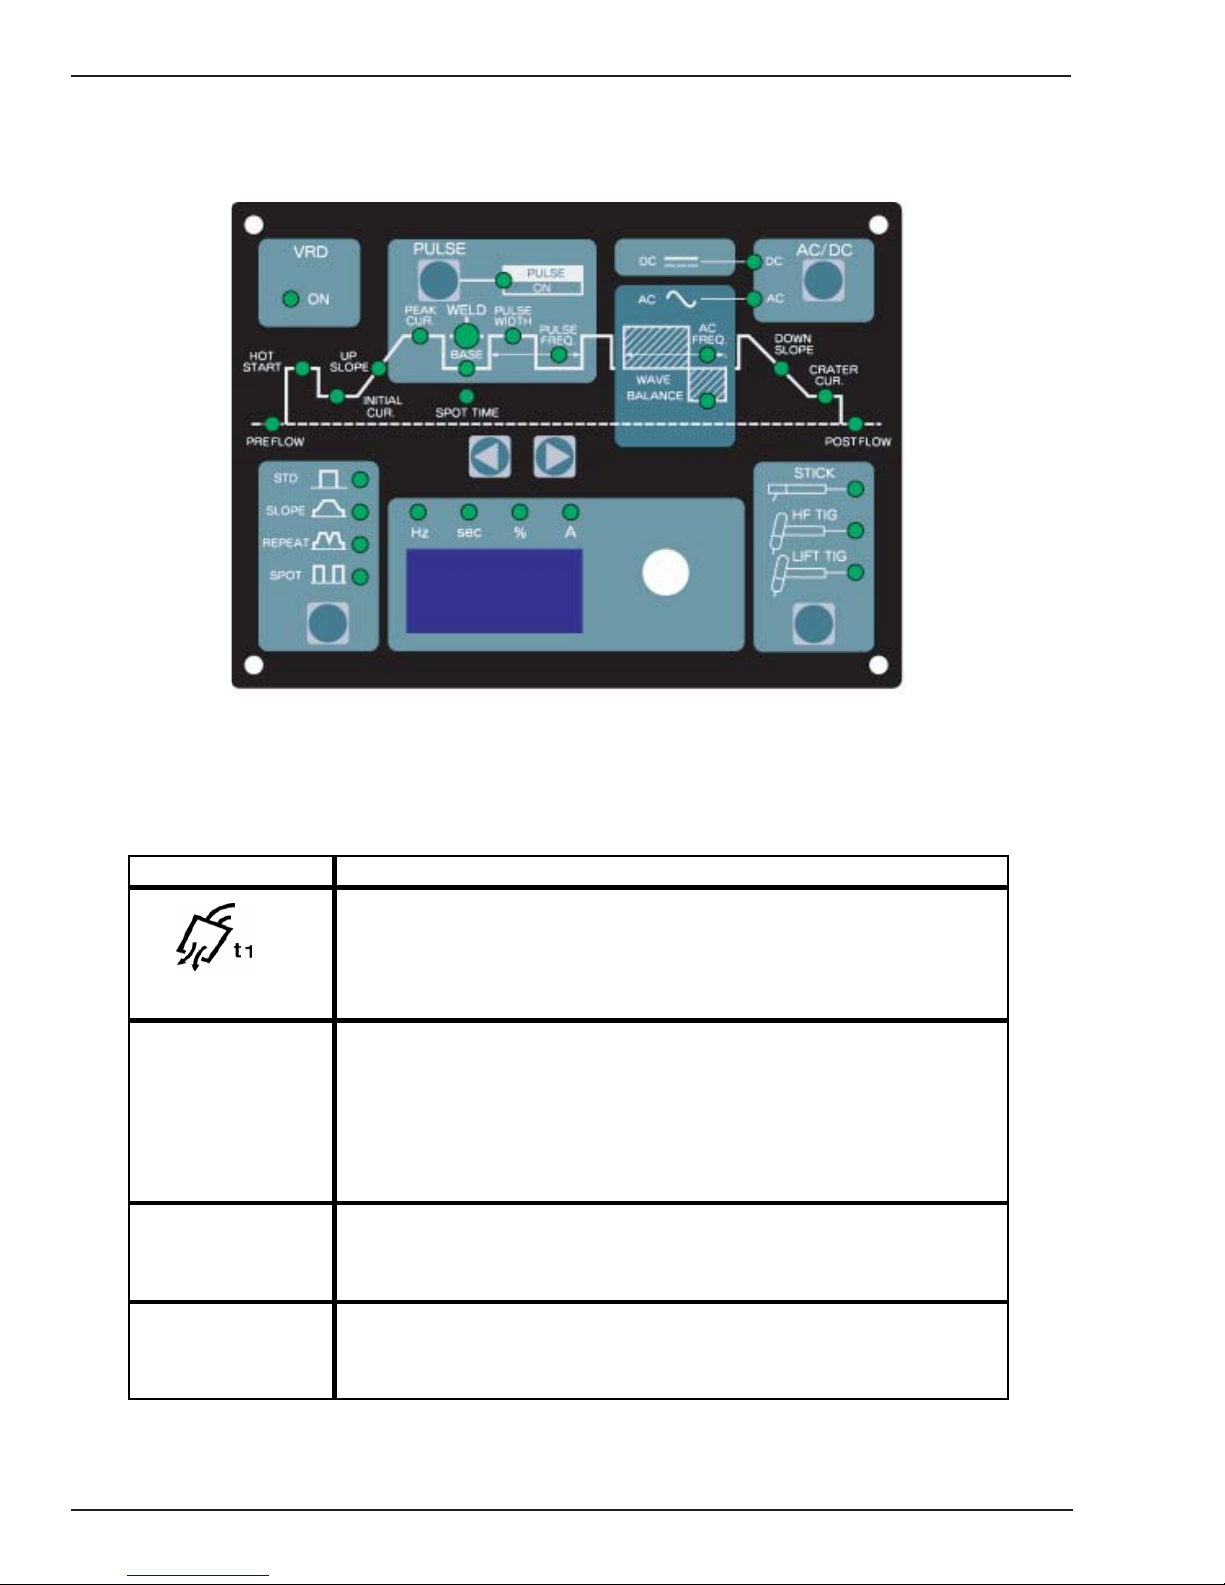
Art # A-04985
Figure 4-3: ArcMaster 300 ACDC Front Panel
Parameter Description
This parameter operates in TIG modes only and is used to provide gas
to the weld zone prior to striking the arc, once the torch trigger switch
has been pressed. This control is used to dramatically reduce weld
PRE-FLOW
porosity at the start of a weld.
This parameter operates in all weld modes except Lift TIG mode and is
used to heat up the weld zone in TIG modes or improve the start
HOT START
INITIAL CUR.
characteristics for stick electrodes. e.g. low hydrogen electrodes. It sets
the peak start current on top of the
HOT START
e.g.
HOT START
This parameter operates in
current = 130 amps when
= 30 amps
SLOPE
BASE (WELD)
or
is used to set the start current for TIG. The Start Current remains on until
the torch trigger switch is released after it has been depressed.
UP SLOPE
This parameter operates in TIG modes only and is used to set the time
for the weld current to ramp up, after the torch trigger switch has been
pressed then released, from INITIAL CUR to PEAK or BASE current
BASE (WELD)
REPEAT
current.
= 100 amps &
(4T) TIG modes only and
Table 4-3: ArcMaster 300 ACDC Front Panel Parameter Description
4-4
February 22, 2006
Page 33
ARCMASTER 300 ACDC
PEAK CUR.
WELD
BASE
(BackgroundCurrent)
SPOT TIME
PULSE WIDTH
PULSE FREQ.
AC FREQUENCY
WAVE BALANCE
This parameter sets the PEAK weld current when in
This parameter sets the TIG WELD current in
SPOT
modes when
PULSE
is off. This parameter also sets the STICK
PULSE
mode
STD, SLOPE, REPEAT
and
weld current.
This parameter sets the Background current when in Pulse TIG mode.
This parameter sets the duration of the
This parameter sets the percentage on time of the
for PEAK weld current when the
This parameter sets the
PULSE FREQUENCY
PULSE
SPOT TIME
is on.
when the
in
HF TIG
mode only
PULSE FREQUENCY
PULSE
is on.
This parameter operates in AC mode only and is used to set the
frequency for the AC weld current.
This parameter is used for aluminum AC TIG mode and is used to set the
penetration to cleaning action ratio for the AC weld current. Generally
WAVE BALANCE
BALANCE
control changes the ratio of penetration to cleaning action of
is set to 50% for AC
STICK
welding. The
WAVE
the AC TIG welding arc. Maximum weld penetration is achieved when
the
WAVE BALANCE
oxidised aluminium or magnesium alloys is achieved when the
BALANCE
WAVE BALANCE=50%
control is set to 65%.
control is set to 10%. Maximum cleaning of heavily
WAVE
WAVE BALANCE=10%
10%50% 65%
(+ )(+ ) (+ )
WAVE BALANCE=65%
DOWN SLOPE
CRATER CUR.
POST-FLOW
(-)(-) (-)
Balanced with 50% penetration
and 50% cleaning
Maximum Penetration and
90%50% 35%
reduced cleaning
Maximum Cleaning and
reduced penetration
This parameter operates in TIG modes only and is used to set the time
for the weld current to ramp down, after the torch trigger switch has
been pressed, to
CRATER CUR.
This control is used to eliminate the
crater that can form at the completion of a weld.
This parameter operates in
SLOPE
or
REPEAT
(4T) TIG modes only and
is used to set the finish current for TIG. The CRATER Current remains on
until the torch trigger switch is released after it has been depressed.
This parameter operates in TIG modes only and is used to adjust the
post gas flow time once the arc has extinguished. This control is used to
dramatically reduce oxidation of the tungsten electrode.
Table 4-3 (continued): ArcMaster 300 ACDC Front Panel Parameter Description
February 22, 2006
4-5
Page 34
ARCMASTER 300 ACDC
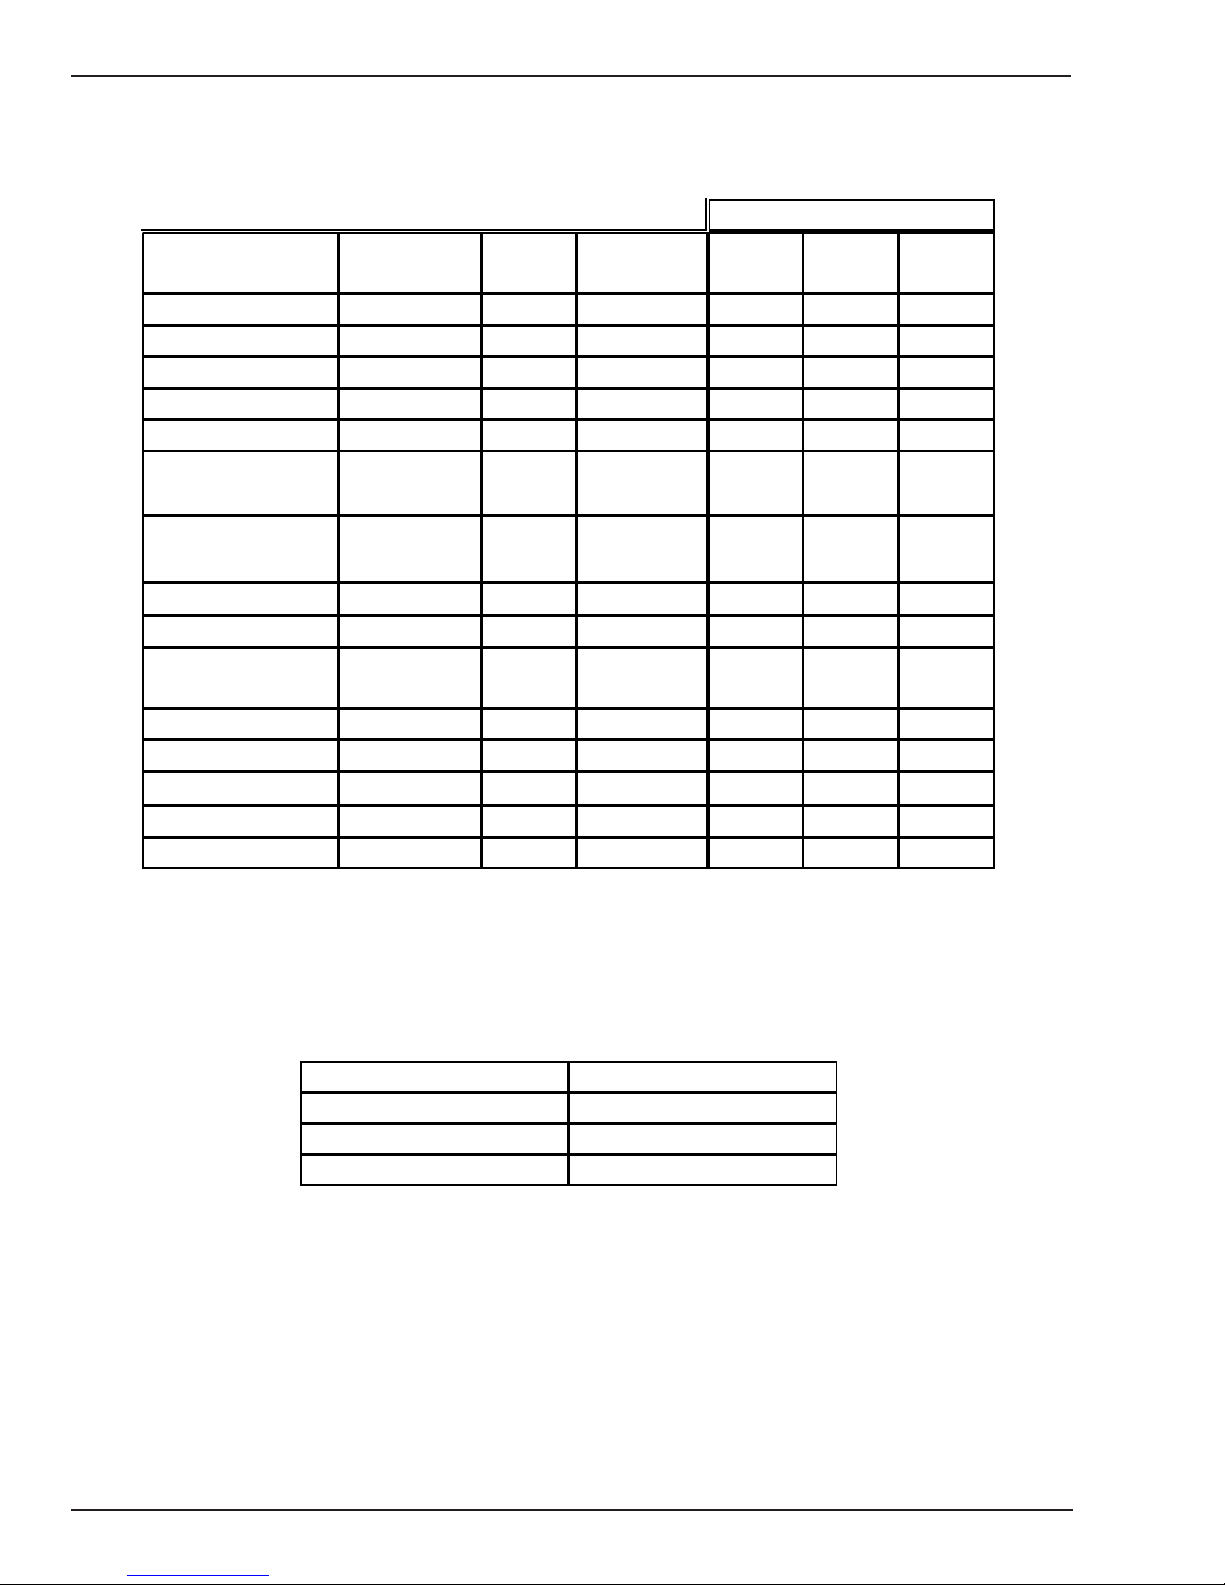
4.04 Weld Parameters for ArcMaster 300 ACDC
Weld HF
Parameter STICK TIG
PRE-FLOW
HOT START
INITIAL CUR.
UP SLOPE
PEAK CUR.
WELD CUR
(TIG)
WELD CUR (STICK)
Parameter
Range
0.0 to 1.0 sec 0.1 sec 0.1 sec No Yes Yes
0 to 70A 20A 1A Yes Yes No
5 to 185A 30A 1A No Yes Yes
0 to 15 sec 1 sec 0.1 sec No Yes Yes
5 to 185A 120A 1A No Yes Yes
5 to 185A 80A
5 to 160A 80A 1A Yes No No
Factory
Setting
Incremental
Unit
1A No
Weld Mode
LIFT TIG
Yes Yes
SPOT TIME
PULSE WIDTH
PULSE FREQ.
AC FREQUENCY
WAVE BALANCE
DOWN SLOPE
CRATER CUR.
POST-FLOW
0.5 to 5.0 sec 2 sec 0.1 sec No Yes Yes
15 to 80% 50% 1% No Yes Yes
0.5 to 500Hz 100.0Hz No
15 to 150Hz 50Hz 1Hz Yes Yes Yes
10 to 65% 50% 1% Yes Yes Yes
0 to 25 sec 3 sec 0.1 sec No Yes Yes
5 to 185A 30A 1A No Yes Yes
0.0 to 60 sec 10 sec 0.1 sec No Yes Yes
Table 4-4: Weld Parameters for ArcMaster 300 ACDC
PULSE FREQ.
0.5 to 20Hz 0.1Hz
20 to 100Hz 1Hz
100 to 500Hz 5Hz
Range Incremental Unit
See
Table 6
Yes Yes
Table 4-5: PULSE FREQ. Range and Incremental Units
4-6
February 22, 2006
Page 35
4.05 Power Source Features
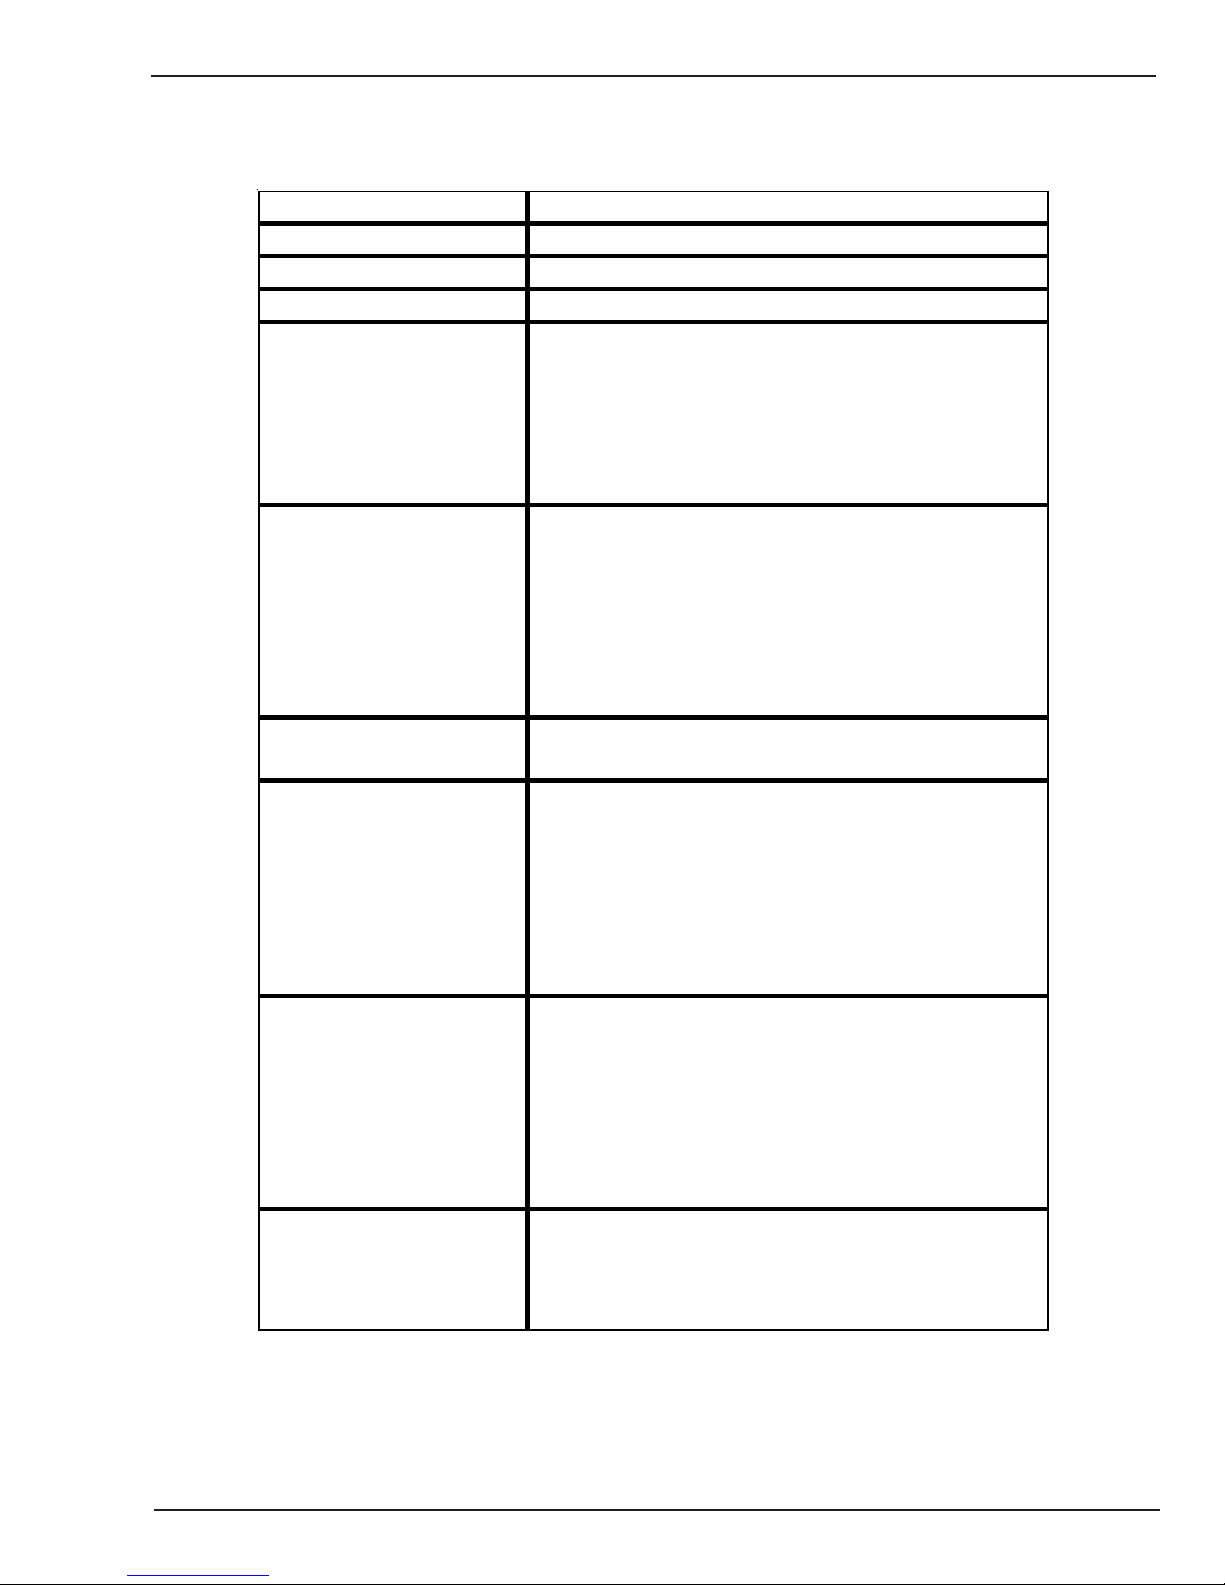
Feature Description
New Digital Control · Almost all welding parameters are adjustable
Touch Panel Switches · Touch switches eliminate mechanical damage
Front Control Cover · Protects front panel controls
Digital Meter
Intelligent Fan Control
ON/OFF switch · Primary voltage Supply ON/OFF switch located on
Voltage Reduction Device
(VRD)
Control Knob
Self Diagnosis Using
Error Codes
ARCMASTER 300 ACDC
· Displays selected weld parameter value
· Displays weld current when welding
· Displays weld current for 20 seconds after weld
has been completed
· A selected weld parameter value can be adjusted
at any time even while welding
· The intelligent cooling system is designed to
reduce dust and foreign material build-up, whilst
providing optimum cooling.
· Fan speed reduces approximately 30 seconds
after machine is turned on
· Fan speed increases when internal components
reaches operating temperature
rear panel
Reduces the OCV when the power supply is not in use.
Eliminates the need for add on voltage reducers and
has no effect on arc starting.
· VRD fully complies to IEC 60974-1
· When Stick mode is selected the green VRD light
is ON when not welding and red when welding.
· When in TIG modes VRD is off.
· For the selected weld parameter, rotating the knob
clockwise increases the parameter
· Rotating the knob counter-clockwise decreases
the parameter
· A selected weld parameter value can be adjusted
at any time even while welding
· Pushing the knob in displays actual arc voltage.
· An error code is displayed on the
when a problem occurs with Primary supply voltage
or internal component problems. Refer to
troubleshooting guide.
Digital Meter
February 22, 2006
Table 4-6:Power Source Features
4-7
Page 36
ARCMASTER 300 ACDC
4-8
February 22, 2006
Page 37
ARCMASTER 300 ACDC
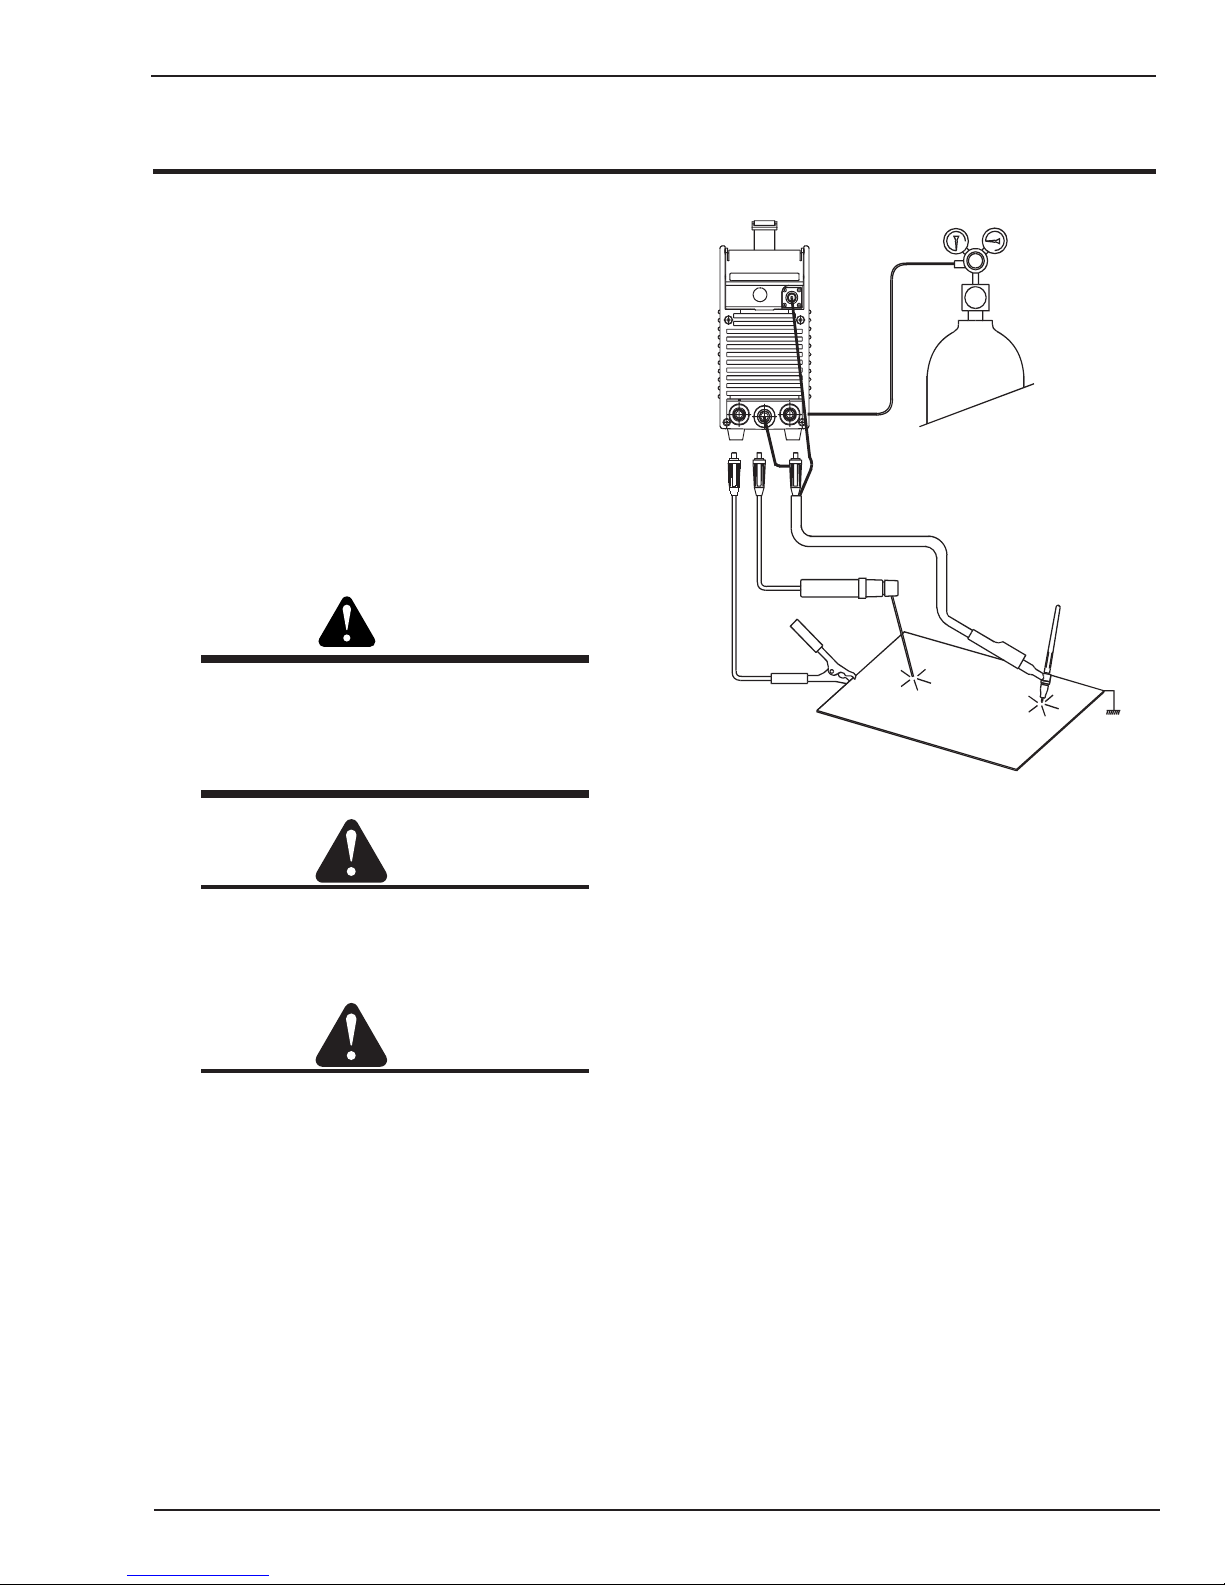
SECTION 5:
SET-UP FOR SMAW (STICK) AND GTAW (TIG)
Conventional operating procedures apply when using the
Welding Power Source, i.e. connect work lead directly to
work piece and electrode lead is used to hold electrode.
Wide safety margins provided by the coil design ensure
that the Welding Power Source will withstand short-term
overload without adverse effects. The welding current
range values should be used as a guide only. Current
delivered to the arc is dependent on the welding arc
voltage, and as welding arc voltage varies between
different classes of electrodes, welding current at any one
setting would vary according to the type of electrode in
use. The operator should use the welding current range
values as a guide, then finally adjust the current setting
to suit the application.
WARNING
Before connecting the work clamp to the work
and inserting the electrode in the electrode
holder make sure the Primary power supply
is switched off.
Art # A-04986
CAUTION
Remove any packaging material prior to use.
Do not block the air vents at the front or rear
or sides of the Welding Power Source.
CAUTION
DO NOT change the Weld Mode or Weld
Process Mode until after POST-FLOW time has
finished.
Figure 5-1: 300 ACDC AC/DC Set-up
February 22, 2006
5-1
Page 38
ARCMASTER 300 ACDC
5-2
February 22, 2006
Page 39
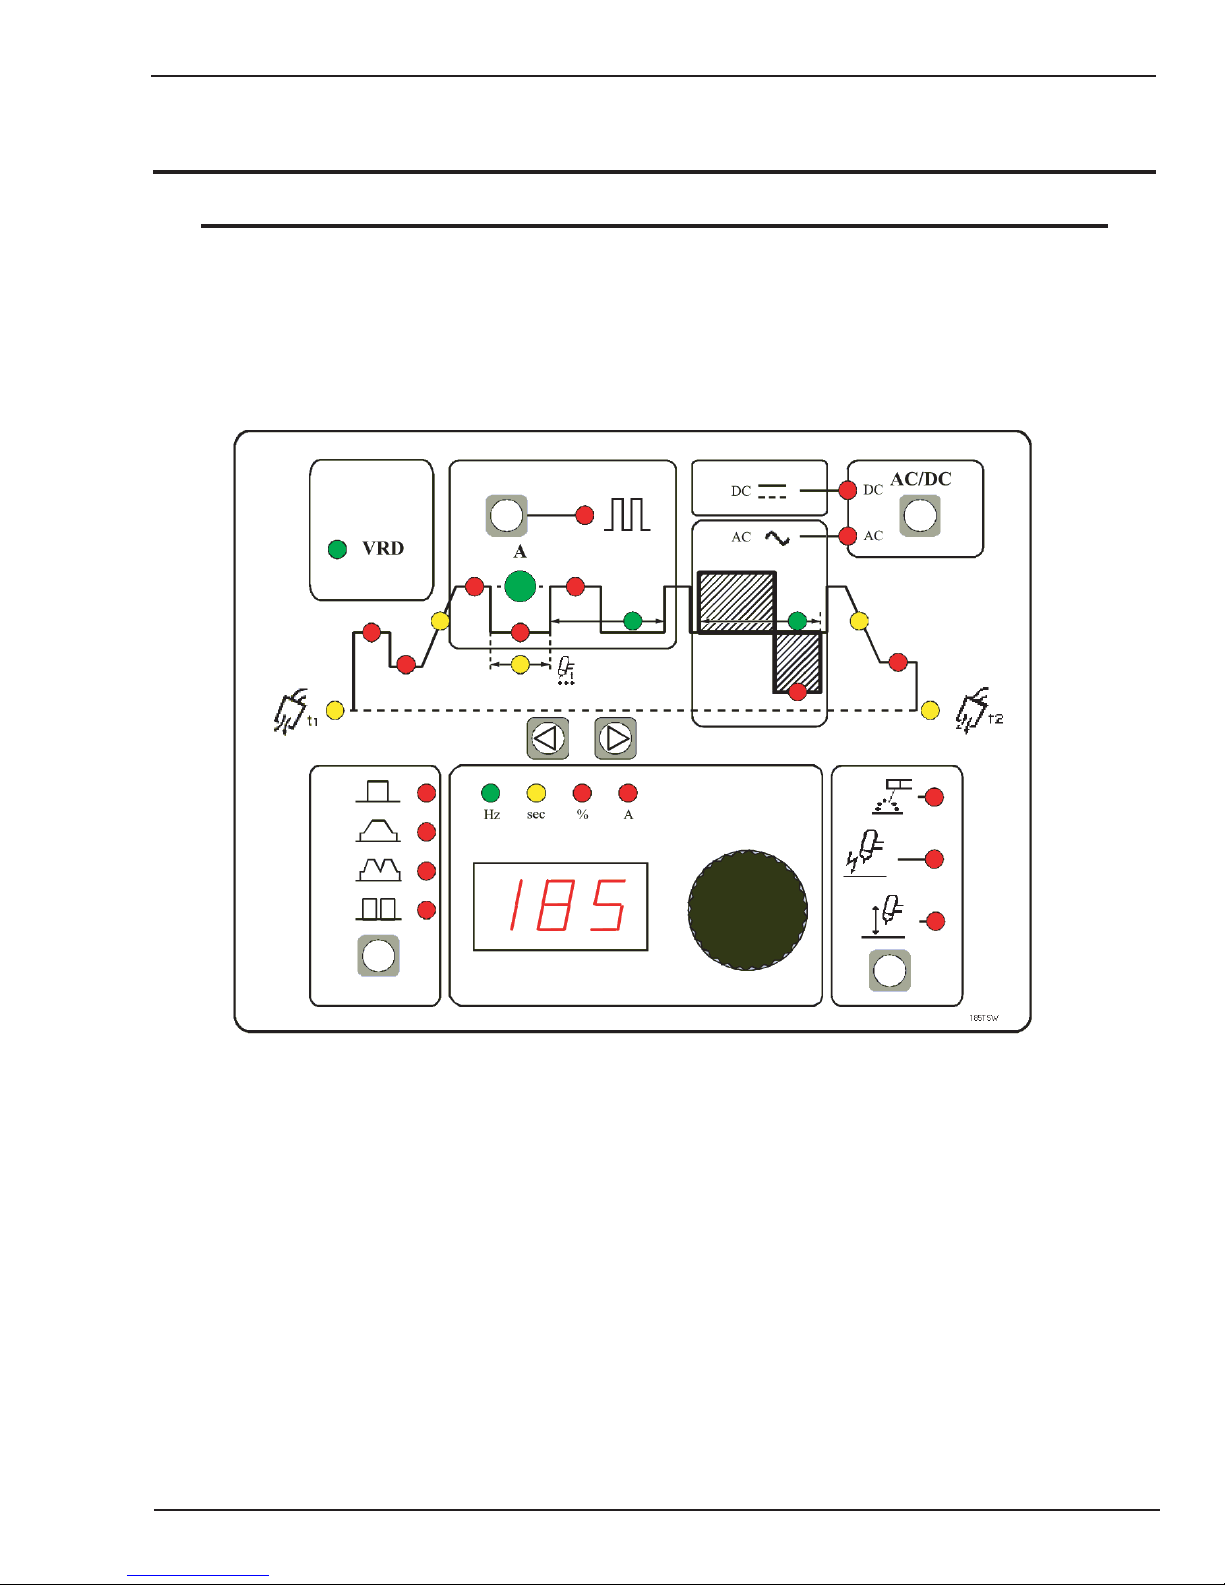
ARCMASTER 300 ACDC
SECTION 6:
SEQUENCE OF OPERATION
NOTE:
Scroll Buttons are used to select the parameters to be set. The LED’s show which function is being
adjusted on the weld sequence graph. Refer to the Symbols Table located in the front of the manual for
Symbol descriptions.
Art # A-04987
February 22, 2006
Figure 6-1a: 300 ACDC Front Panel
6-1
Page 40
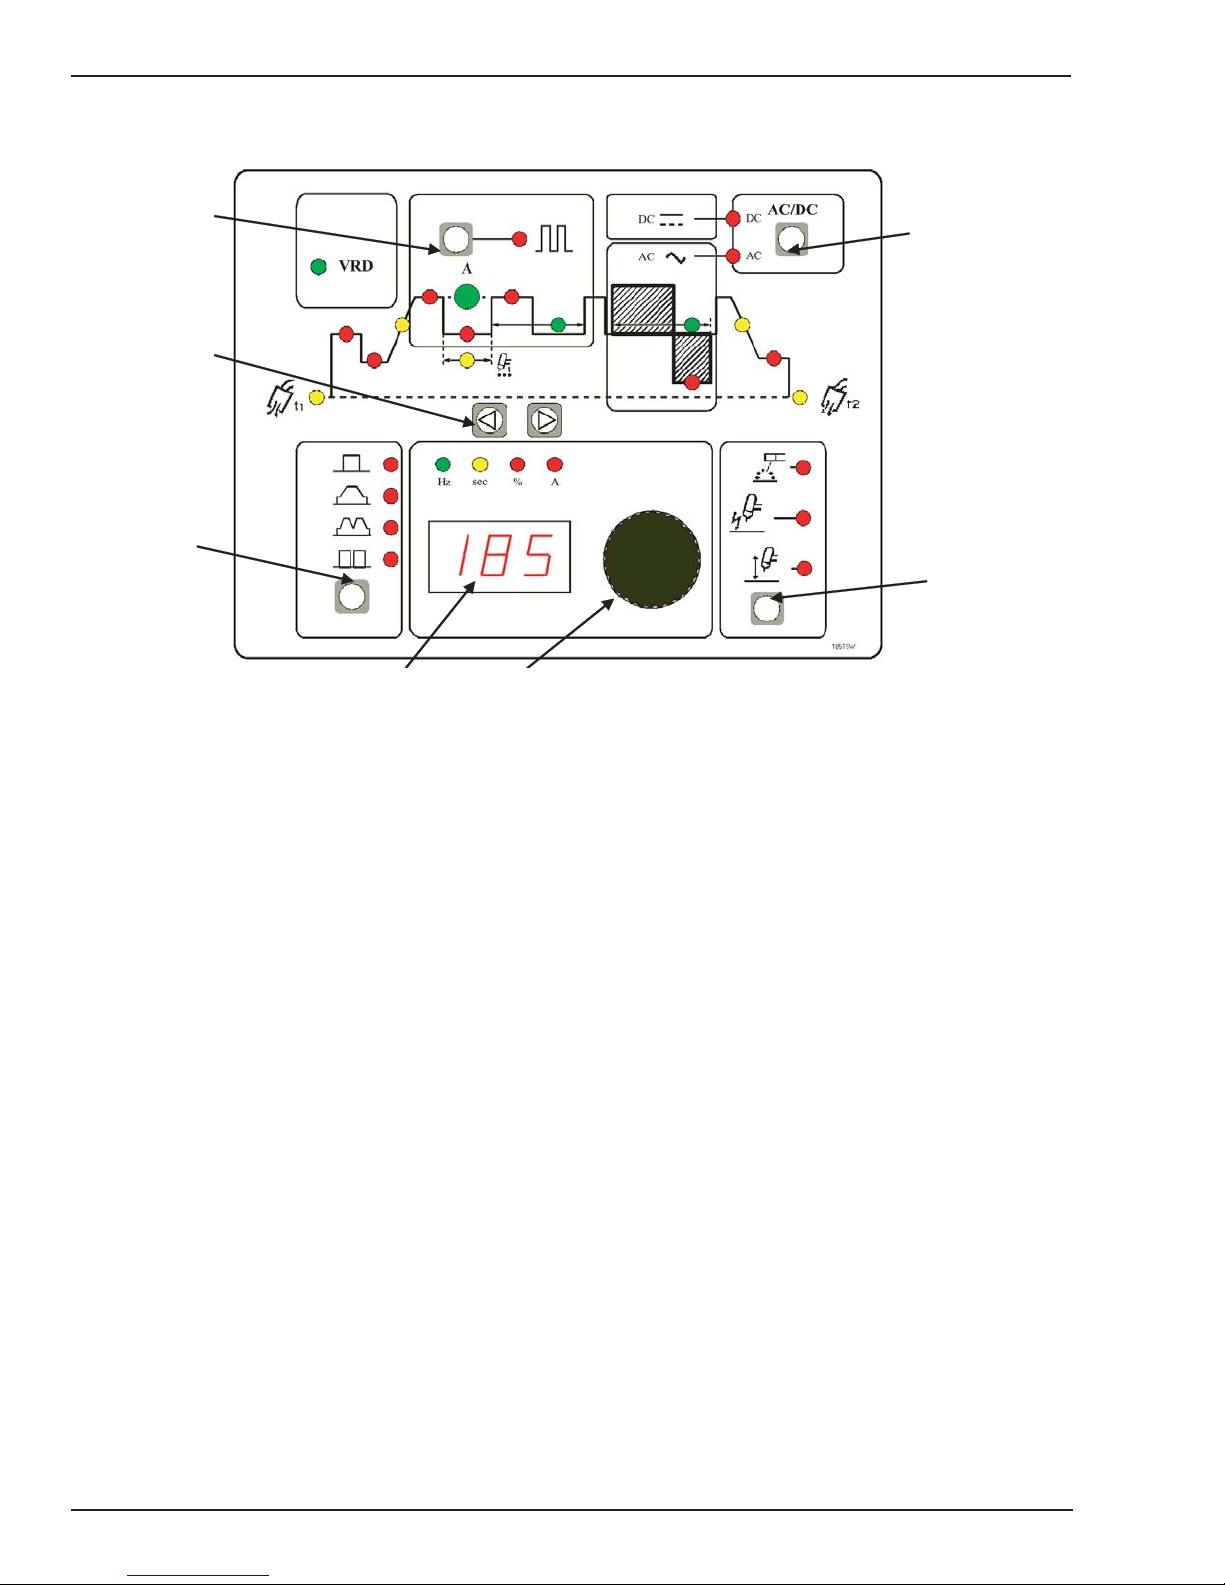
ARCMASTER 300 ACDC
3
1
2
Art # A-04988
7
6
4
5
Figure 6-1b: 300 ACDC Front Panel
1. Pulse function: Pressing this button enables the TIG
current pulse functions.
2. Scroll Buttons: used to select the parameters to be
set. The LED’s show which function is being adjusted
on the Sequence Graph.
3. TIG Mode Functions : Pressing this button scrolls
through the output TIG function modes (Standard,
Slope, Slope w/repeat, Spot).
4. Digital LED display : Welding amperage and
parameter values are displayed in this window.
Internal warnings such as over temperature, low or
high input voltage applied are signaled to the operator
by a warning sound and error message on the screen.
5. Control knob: allows the operator to adjust the output
amperage within the entire range of the power source,
also used to set each parameter value. Pushing the
knob inward displays the actual welding voltage.
6. Process Button: This button selects between STICK,
Lift or HF TIG mode. A remote control device is
required for use during LIFT TIG and HF TIG operation.
See section 4.01, 2.Remote Control Socket, for
complete details of the remote device.
7. AC/DC Button: Selects between AC or DC welding
output.
6-2
February 22, 2006
Page 41
ARCMASTER 300 ACDC
6.01 Stick Welding
· Connect work lead to negative terminal
· Connect electrode lead to positive terminal
· Switch machine on
· Set
AC
or DC weld current. If AC is selected then set
AC FREQ
· Connect remote control device if required.
Use the Scroll Buttons to move to the parameter to be
set. The LED will show which function is being adjusted
on the weld sequence graph. Use the control knob to
adjust each parameter.
· Set
· Set
Commence welding
to 60Hz &
HOT START
WELD
current
WAVE BALANCE
to 50%.
6.02 AC or DC HF TIG Welding
· Connect work lead to positive terminal
· Connect TIG torch to negative terminal
· Switch machine on
· Set
AC
or DC weld current. If AC is selected then set
AC FREQ
· Connect remote control device. . See section 4.01,
2. Remote Control Socket, for complete details of
the remote device.
Use the Scroll Buttons to move to the parameter to be
set. The LED will show which function is being adjusted
on the weld sequence graph. Use the control knob to
adjust each parameter.
· Set
· Set
· Set
· Set
&
WAVE BALANCE
PRE-FLOW
HOT START
POST-FLOW
WELD
current
time
current
time
· Set
POST-FLOW
Slope Mode Parameters if required
· Set
INITIAL CUR
· Set
UP SLOPE
· Set (WELD)
· Set
BASE
· Set
DOWN SLOPE
· Set
CRATER CUR
Pulse Mode parameters if required
· Set
PULSE WIDTH
·
Set PEAK CURRENT
· Set
PULSE FREQ
Commence welding
time
PEAK CUR
current
time
current
time
current
% for
current
PEAK CURRENT
February 22, 2006
6-3
Page 42
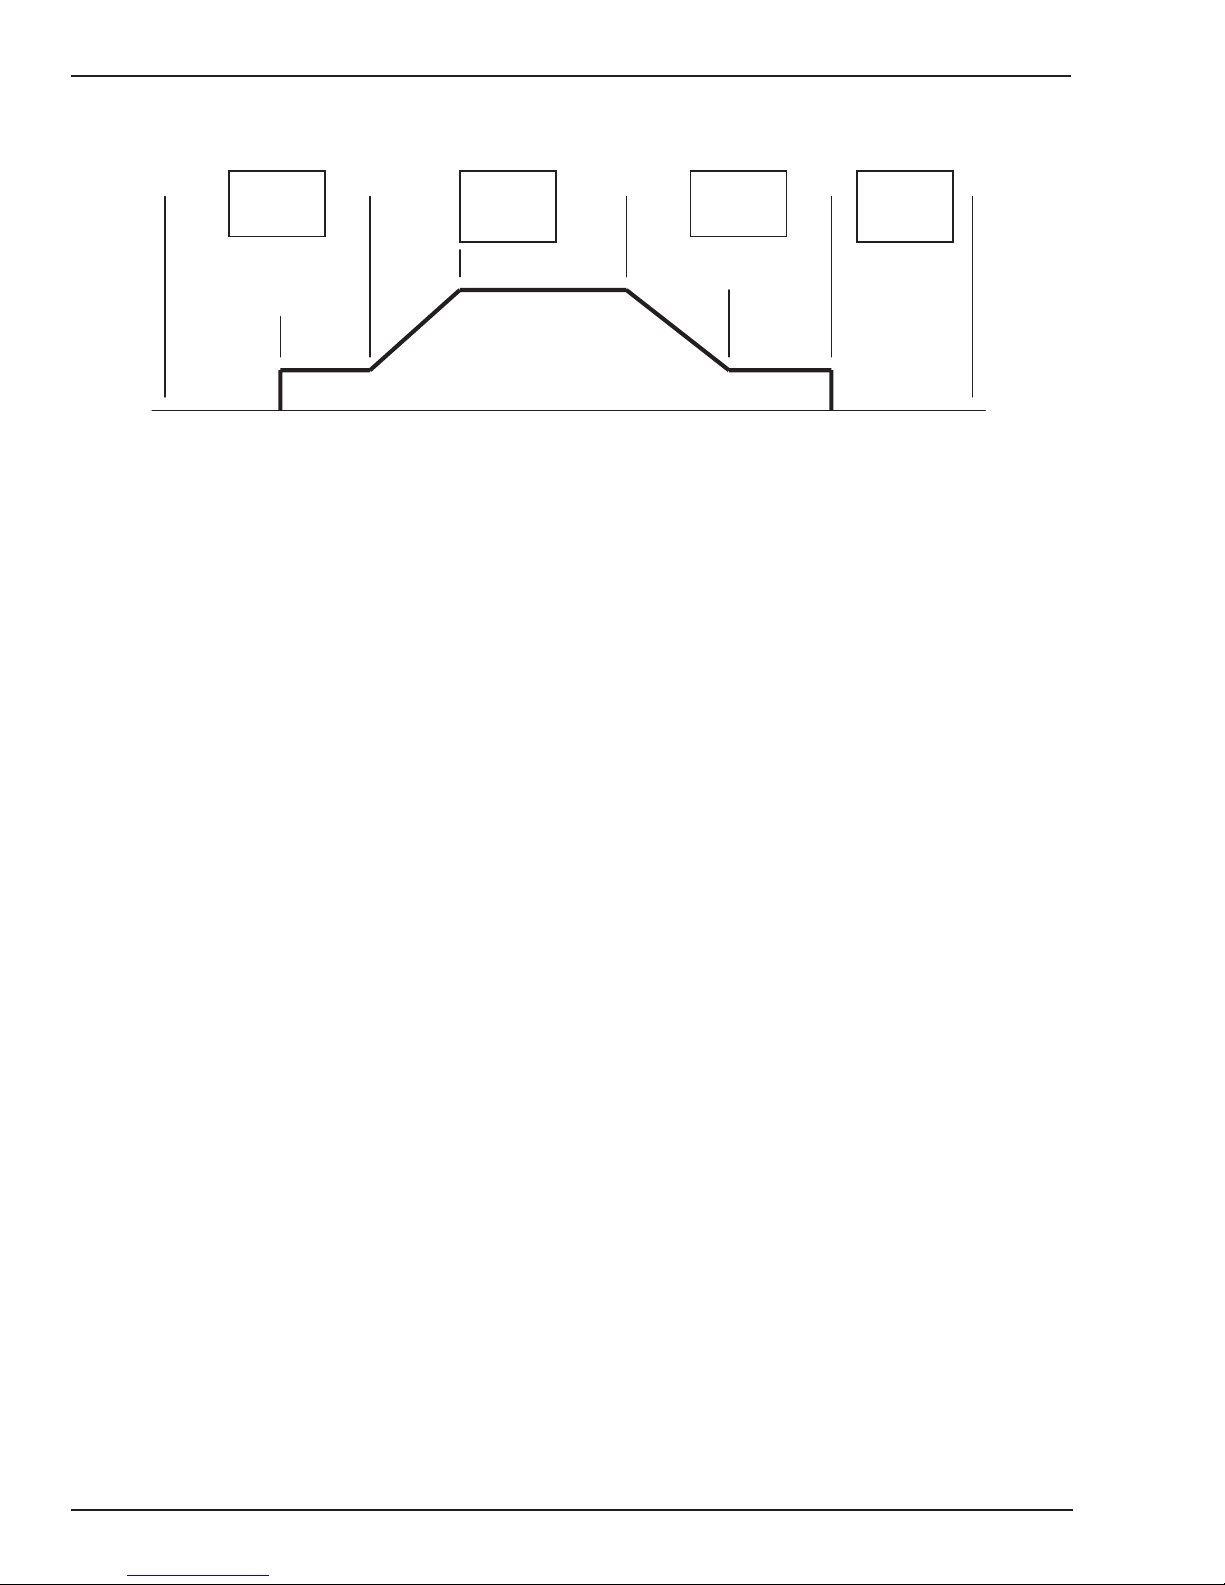
ARCMASTER 300 ACDC
6.03 Slope Mode Sequence
Switch
Closed
Switch
Open
Switch
Closed
Art # A-04989
Switch
Open
Initial
Up
Slope
Weld Current
Current
Preflow
Figure 6-2: Slope Mode Sequence
1. To start Slope sequence Close remote switch contacts.
Once the welding arc is established the Power Source
will maintain initial current setting as long as the
remote switch contacts are closed.
a. In the HF TIG mode, after Preflow time, High
Frequency is present at the torch. When the torch
is positioned close to the work the welding current
will transfer to the work and establish the arc at
the initial current setting.
b. In the Lift TIG mode, after Preflow time, Lift Start
current is present at the torch. When the electrode
is touched to the work and lifted off, the welding
arc is established at the initial current setting.
Down
Slope
Final
Current
Postflow
2. Open Remote Switch – current increases to weld
current. Once welding arc has reached weld current
the power source will maintain weld current as long
as the remote switch contacts are open.
3. Close Remote Switch – Welding current decreases to
final current setting. Once final welding current is
reached the power source will maintain final current
setting as long as the remote switch contacts are
closed.
4. Open Remote Switch – Welding arc stops and post
flow begins.
6.04 Slope Mode with repeat sequence
The repeat function is operated during the down slope
cycle of the Slope Sequence and is active through the
down slope period only. During the down slope period,
by opening the Remote Switch contacts, the current will
increase back to weld current. Within the Down Slope
period the repeat function can be operated as many times
as desired. To continue slope cycle and end slope
sequence close remote switch contacts and allow weld
current to reach final current setting. Once final current
setting is reached, opening the Remote Switch again will
turn off the welding arc and post flow begins.
6-4
February 22, 2006
Page 43
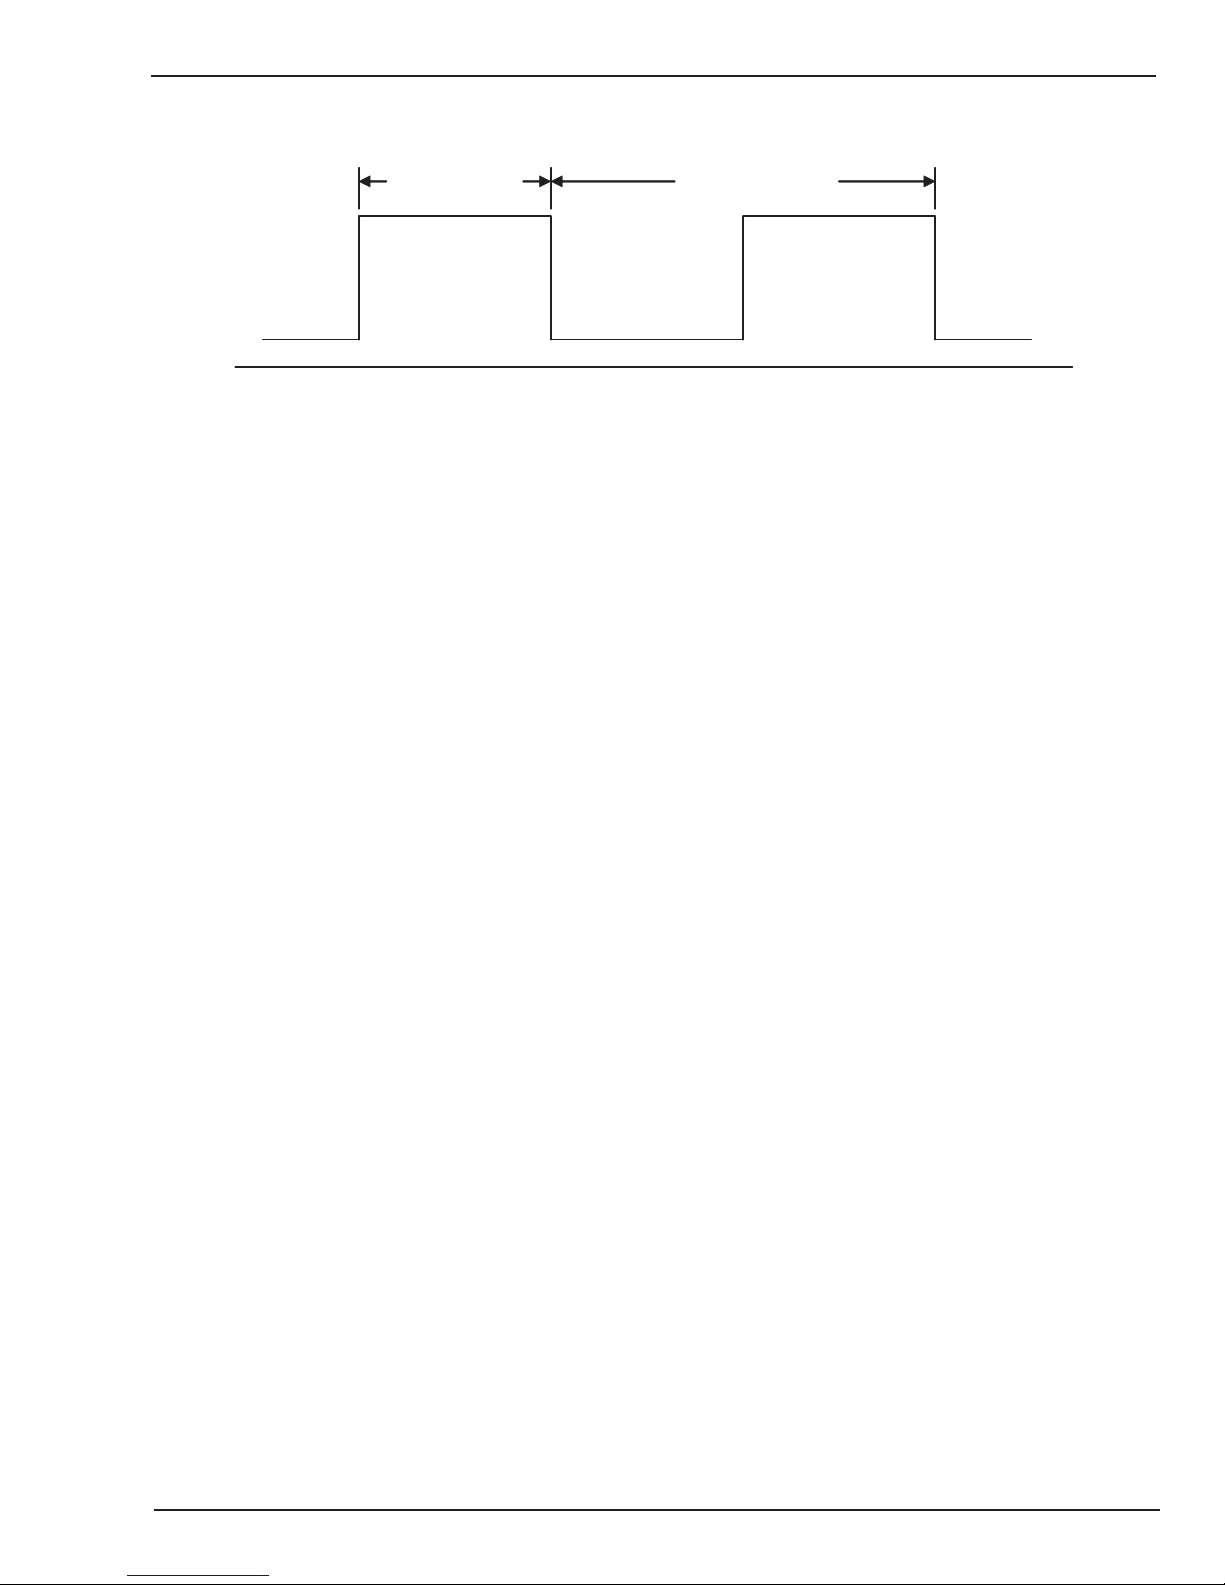
6.05 Pulse Controls
ARCMASTER 300 ACDC
(Pulse Width) (Pulse Frequency)
Art # A-04990
(Peak Current)
(Base)
Background
Current
Figure 6-3: Pulse Controls
The Pulse controls are used primarily to control heat input. Pulse offers a number of advantages as follows:
1) Control puddle – size and fluidity (especially out of position).
2) Increase penetration
3) Travel speed control
4) Better consistent quality
5) Decreased distortion on lighter or thinner materials.
Pulse-current provides a system in which the welding current continuously changes between two levels. During the
periods of Peak current, heating and fusion takes place, and during the background (base) current periods, cooling
and solidification take place. Pulse Width is the time in one cycle the current remains at the peak current setting.
Pulse Frequency, measured in Hertz, is the number of cycles per second the current travels between peak and background
current settings. It is as if the foot rheostat were moved up and down to increase and decrease the welding current on
a regular basis. The faster you moved the foot rheostat up and down the faster the frequency.
February 22, 2006
6-5
Page 44
ARCMASTER 300 ACDC
6-6
February 22, 2006
Page 45
SECTION 7:
BASIC TIG WELDING GUIDE
ARCMASTER 300 ACDC
7.01 Explanation of “Fluttery Arc” when
AC TIG Welding on Aluminum
The following will assist in understanding the
phenomenon of Arc Flutter, also referred to as Arc
Rectification.
The basic thesis is that the fluttering is caused by lack of
oxide in the weld pool.
The oxide layer on the plate reduced the energy for
electron emission. Electron emission from the weld pool
(DC+) causes the oxide layers to be disrupted, the socalled “cleaning action”. However once the cleaning action
has produced a mirror like surface on the weld pool, the
effect of the oxide layer is limited because the oxide layer
has dissipated. This makes electron emission from the
weld pool more difficult and increases the chance of arc
instability.
AC TIG on aluminum
1. The Problem: Arc appears unstable and pulses or flutters. ie. appears to rapidly change welding current
This idea is supported by the observation that once
fluttering starts it can be made to stop by working the arc
away from the mirror like weld pool to an area of oxide
coated material. As soon as this is done the arc settles
back to a stable condition. So while the arc is “consuming”
oxide coated plate the instability does not occur. But once
the arc is stationary, the pool becomes thoroughly
“cleaned” by election emission, the fluttering begins.
Tests conducted on various types of AC TIG power
sources, Fluttery Arc is not confined to one type of power
source or it’s design, both conventional and inverter types
suffer from the same problem.
.
Conditions that accentuate arc flutter: Conditions that minimizes arc flutter:
· Cold work piece, · Preheat the work piece,
· Very short arc length, · Increase the arc length,
· Weld pool crater about 0.39” to
0.47” (10 to 12mm) diameter,
· Arc field in one spot to produce
“mirror” clean weld pool,
· Increased cleaning action.
ie. Prolonged oxide emission from a
stationary weld pool increases the
likelihood of arc flutter,
· Accentuated when tungsten running
near its current capacity, ie. Molten ball
on end.
Table 7-1: Reduction of Arc Flutter
2. Conclusion: Fluttery arc in AC TIG is a physical phenomenon independent of machine design.
· Introduce filler rod material to the
weld pool, which introduces oxides.
· Move the weld pool around to
introduce oxides to the weld pool.
· Decrease the cleaning action by
turning the
50% or move the weld pool around.
· Use a larger diameter tungsten
electrode.
WAVE BALANCE
to below
February 22, 2006
7-1
Page 46
ARCMASTER 300 ACDC
7.02 Electrode Polarity
Connect the TIG torch to the - / TORCH terminal and the work lead to the + / WORK terminal for direct current straight
polarity. Direct current straight polarity is the most widely used polarity for DC TIG welding. It allows limited wear of
the electrode since 70% of the heat is concentrated at the work piece.
7.03 Tungsten Electrode Current Ranges
Electrode Diameter AC Current (Amps) DC Current (Amps)
0.040” (1.0mm) 30 – 70 30 – 60
1/16” (1.6mm) 60 – 95 60 – 115
3/32” (2.4mm) 125 – 150 100 – 165
1/8” (3.2mm) 130 – 225 135 – 200
5/32” (4.0mm) 190 – 280 190 – 280
3/16” (4.8mm) 250 – 340 250 – 340
Table 7-2: Current ranges for various tungsten electrode sizes
7.04 Tungsten Electrode Types
Electrode Type
(Ground Finish)
Thoriated 2%
Zirconated 1%
Ceriated 2%
Welding Application Features Color
DC welding of mild steel,
stainless steel and copper.
High quality AC welding of
aluminium, magnesium and
their alloys.
AC & DC welding of mild steel,
stainless steel, copper,
aluminium, magnesium and
their alloys
Table 7-3: Tungsten electrode types
Excellent arc starting, Long life,
High current carrying capacity.
Self cleaning, Long life,
Maintains balled end, High
current carrying capacity.
Longer life, More stable arc,
Easier starting, Wider current
range, Narrower more
concentrated arc.
Code
Red
White
Grey
7-2
Februrary 22, 2006
Page 47
ARCMASTER 300 ACDC
7.05 Guide for Selecting Filler Wire Diameter
NOTE
The filler wire diameter specified in Table 7-4 is a guide only, other diameter wires may be used according
to the welding application
Filler Wire Diameter
1/16” (1.6 mm) 30-95 20 - 90
3/32” (2.4 mm) 125-160 65 - 115
1/8” (3.2 mm) 180-240 100 - 165
3/16” (4.8 mm) 220-320 200-350
7.06 Shielding Gas Selection
Alloy
Aluminium & alloys Welding Argon, Argoshield 80T, 81T
Carbon Steel Welding Argon
Stainless Steel Welding Argon, Argoshield 71T, 80T, 81T
Nickel Alloy Welding Argon, Argoshield 71T
Copper Welding Argon, Argoshield 81T
Titanium Welding Argon, Argoshield 80T, 81T
AC Current Range DC Current Range
(Amps) (Amps)
Table 7-4: Filler wire selection guide
Shielding Gas
Argoshield is a registered trademark of BOC Gases
Limited.
Table 7-5: Shielding gas slection
7.07 TIG Welding Parameters for Low Carbon & Low Alloy Steel Pipe
Electrode Type &
Diameter
Thoriated 2%
3/32” (2.4 mm)
Thoriated 2%
3/32” (2.4 mm)
Thoriated 2%
3/32” (2.4 mm)
Table 7-6: TIG welding parameters for low carbon & low alloy steel pipe
Current Range DC
Amperes
120 - 170 Yes
100 - 160 Yes
90 - 130 No
Filler Rod for
Root Pass
Joint Preparation
February 22, 2006
7-3
Page 48
ARCMASTER 300 ACDC
7.08 Welding Parameters for Aluminum
Base Metal
Thickness
0.040” 30-45 0.040” 1/16” Butt/Corner
1.0mm 35-50 1.0mm 1.6mm Lap/ Fillet
0.045” 40-60 0.040” 1/16” Butt/Corner
1.2mm 45-70 1.0mm 1.6mm Lap/ Fillet
1/16” 60-85 1/16” 1/16” Butt/Corner
1.6mm 70-95 1.6mm 1.6mm Lap/ Fillet
1/8” 3/32” 3/32”
3.2mm 2.4mm 2.4mm
3/16” 180-225 1/8” 1/8” Butt/Corner
4.8mm 190-240 3.2mm 3.2mm Lap/ Fillet
¼” 240-280 3/16” 3/16” Butt/Corner
6.4mm 250-320 4.8mm 4.8mm Lap/ Fillet
AC Current for
Aluminum
125-150
130-160
Table 7-7: AC TIG welding parameters
Tungsten
Electrode
Diameter
1/8”
3.2mm
Filler Rod
Diameter
(if required)
Argon Gas
Flow Rate
Liters/min
5-7
5-7
7
10
10
13
Joint Type
Butt/Corner
Lap/Fillet
7.09 Welding Parameters for Steel
Base Metal
Thickness
0.040” 35-45 20-30 0.040” 1/16” Butt/Corner
1.0mm 40-50 25-35 1.0mm 1.6mm Lap/ Fillet
0.045” 45-55 30-45 0.040” 1/16” Butt/Corner
1.2mm 50-60 35-50 1.0mm 1.6mm Lap/ Fillet
1/16” 60-70 40-60 1/16” 1/16” Butt/Corner
1.6mm 70-90 50-70 1.6mm 1.6mm Lap/ Fillet
1/8” 80-100 65-85 1/16” 3/32” Butt/Corner
3.2mm 90-115 90-110 1.6mm 2.4mm Lap/ Fillet
3/16” 115-135 100-125 3/32” 1/8” Butt/Corner
4.8mm 140-165 125-150 2.4mm 3.2mm Lap/ Fillet
¼” 160-175 135-160 1/8” 5/32” Butt/Corner
6.4mm 170-200 160-180 3.2mm 4.0mm Lap/ Fillet
DC Current
for Mild
Steel
DC Current for
Stainless
Steel
Tungsten
Electrode
Diameter
Filler Rod
Diameter
(if required)
Argon Gas
Flow Rate
Liters/min
5-7
5-7
7
7
10
10
Joint Type
Table 7-8: DC TIG welding parameters
7-4
Februrary 22, 2006
Page 49
SECTION 8:
BASIC ARC WELDING GUIDE
8.01 Electrode Polarity
Stick electrodes are generally connected to the ‘+’ terminal
and the work lead to the ‘-’ terminal but if in doubt consult
the electrode manufacturers literature.
8.02 Effects of Stick Welding Various
Materials
ARCMASTER 300 ACDC
1. High tensile and alloy steels: The two most prominent
effects of welding these steels are the formation of a
hardened zone in the weld area, and, if suitable
precautions are not taken, the occurrence in this zone
of under-bead cracks. Hardened zone and under-bead
cracks in the weld area may be reduced by using the
correct electrodes, preheating, using higher current
settings, using larger electrodes sizes, short runs for
larger electrode deposits or tempering in a furnace.
2. Manganese steels: The effect on manganese steel of
slow cooling from high temperatures is to embrittle
it. For this reason it is absolutely essential to keep
manganese steel cool during welding by quenching
after each weld or skip welding to distribute the heat.
3. Cast Iron: Most types of cast iron, except white iron,
are weldable. White iron, because of its extreme
brittleness, generally cracks when attempts are made
to weld it. Trouble may also be experienced when
welding white-heart malleable, due to the porosity
caused by gas held in this type of iron.
4. Copper and alloys: The most important factor is the
high rate of heat conductivity of copper, making
preheating of heavy sections necessary to give proper
fusion of weld and base metal.
5. Types of Electrodes: Arc Welding electrodes are
classified into a number of groups depending on their
applications. There are a great number of electrodes
used for specialized industrial purposes, which are
not of particular interest for everyday general work.
These include some low hydrogen types for high
tensile steel, cellulose types for welding large diameter
pipes, etc. The range of electrodes dealt with in this
publication will cover the vast majority of applications
likely to be encountered; are all easy to use and all will
work on even the most basic of welding machines.
February 22, 2006
8-1
Page 50
ARCMASTER 300 ACDC
Metals being
Electrode Comments
joined
Mild steel 6013 Ideal electrodes for all general purpose work.
Features include out standing operator appeal,
easy arc starting and low spatter.
Mild steel 7014 All positional electrode for use on mild and
galvanized steel furniture, plates, fences, gates,
pipes and tanks etc. Especially suitable for
vertical-down welding.
Cast iron 99% Nickel Suitable for joining all cast irons except white cast
iron.
Stainless steel 318L-16 High corrosion resistance. Ideal for dairy work,
etc. On stainless steels.
Copper, Bronze,
Brass, etc.
Bronze
5.7 ERCUSI-A
Easy to use electrode for marine fittings, water
taps and valves, water trough float arms, etc.
Also for joining copper to steel and for bronze
312-16High Alloy Steels,
Dissimilar Metals,
Crack Resistance.
All Hard-To-Weld
It will weld most problematical jobs such as
springs, shafts, broken joins mild steel to
stainless and alloy steels.
Not suitable for Aluminum.
Table 8-1: Types of Electrodes
8-2
February 22, 2006
Page 51
ARCMASTER 300 ACDC
SECTION 9:
ROUTINE MAINTENANCE
The only routine maintenance required for the power supply is a thorough cleaning and inspection, with the frequency
depending on the usage and the operating environment.
WARNING
Disconnect primary power at the source before opening the enclosure. Wait at least two minutes before
opening the enclosure to allow the primary capacitors to discharge.
To clean the unit, open the enclosure and use a vacuum cleaner to remove any accumulated dirt and dust. The unit
should also be wiped clean, if necessary; with solvents that are recommended for cleaning electrical apparatus.
CAUTION
Do not blow air into the power supply during cleaning. Blowing air into the unit can cause metal particles to
interfere with sensitive electrical components and cause damage to the unit.
February 22, 2006
9-1
Page 52
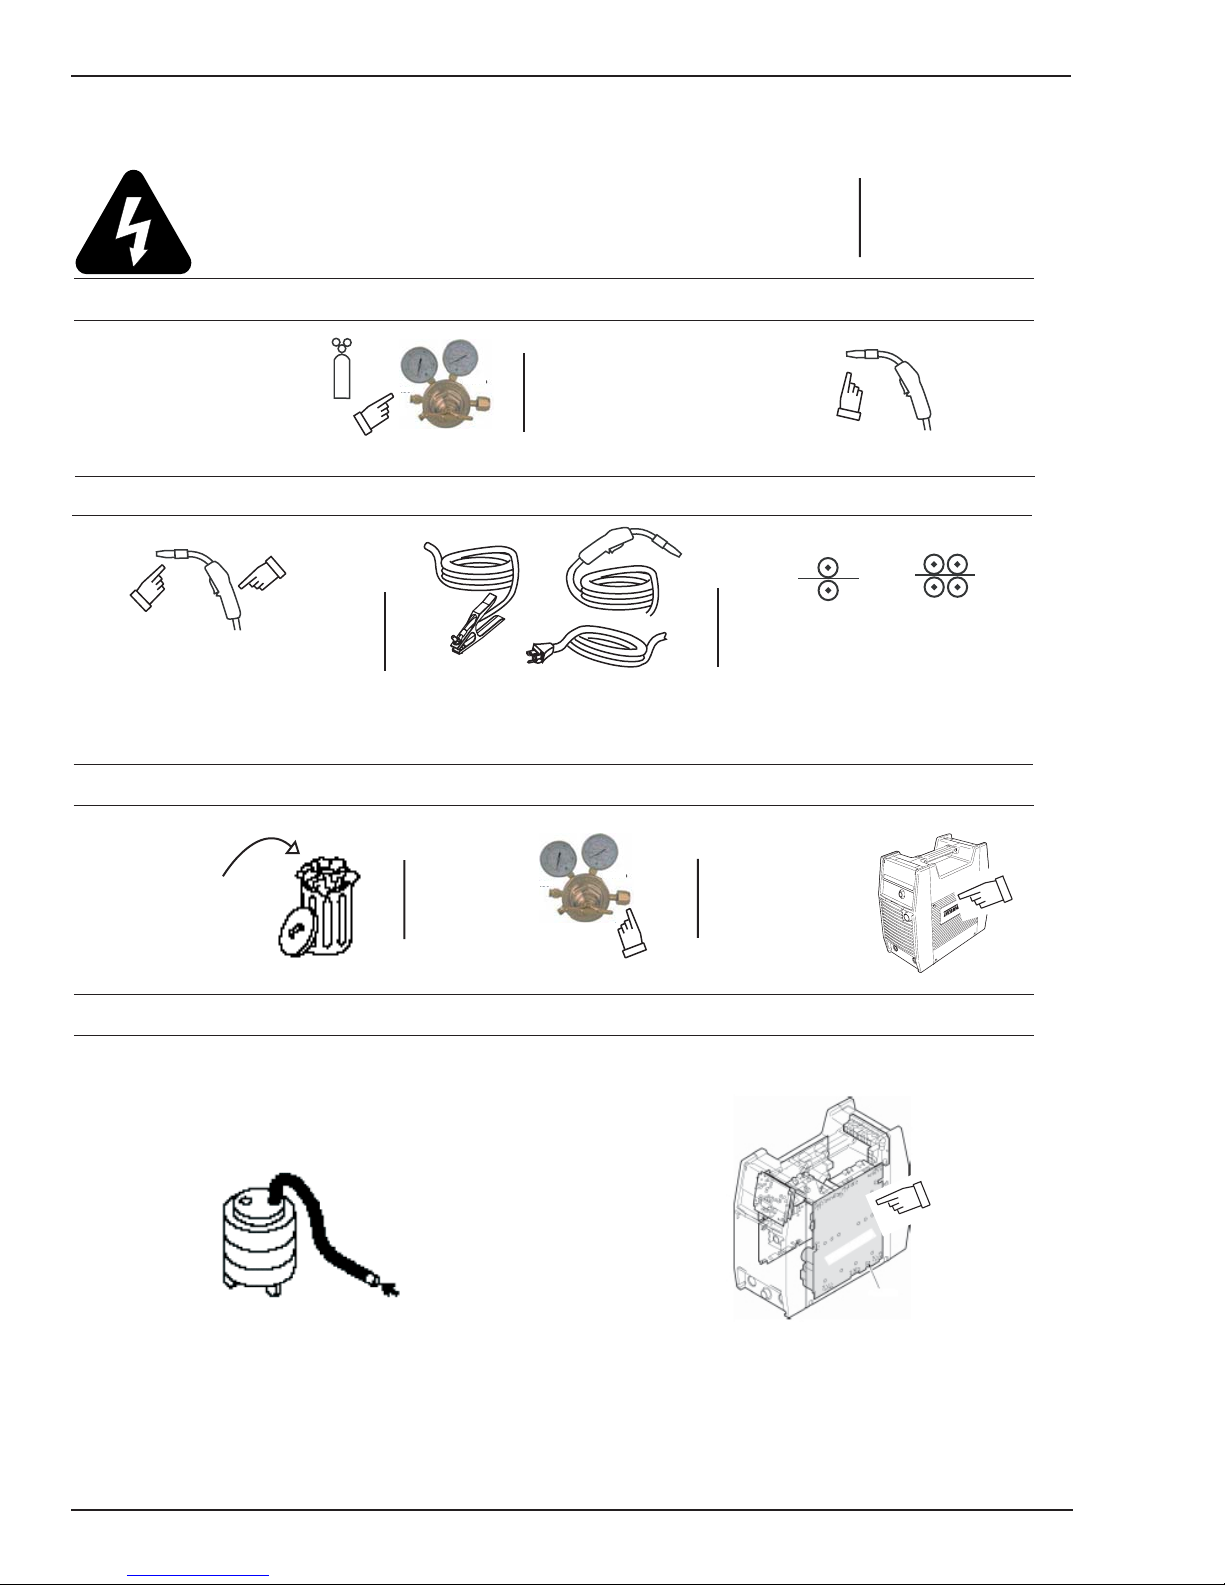
ARCMASTER 300 ACDC
Warning!
Disconnect input power before maintaining.
Visual check of
regulator and pressure
Visually inspect the torch
body and consumables
Each Use
Visual check of torch
Consumable parts
Weekly
Visually inspect the
cables and leads.
Replace as needed
Maintain more often
if used under severe
conditions
Visually inspect the Wire
feed mechanisms
Replace all
broken parts
3 Months
Gas and
air lines
6 Months
Visually check and
use a vacuum to carefully
clean the interior
Clean
exterior
of power supply
Art # A-06950
9-2
February 22, 2006
Page 53
ARCMASTER 300 ACDC
g
p
j
SECTION 10:
BASIC TROUBLESHOOTING
WARNING
There are extremely dangerous voltages and power levels present inside this product. Do not attempt to
open or repair unless you are an Accredited Thermal Arc Service Agent and you have had training in power
measurements and troubleshooting techniques.
If major complex subassemblies are faulty, then the Welding Power Source must be returned to an Accredited Thermal
Arc Service Agent for repair.
The basic level of troubleshooting is that which can be performed without special equipment or knowledge.
10.01 TIG Welding Problems
Weld quality is dependent on the selection of the correct consumables, maintenance of equipment and proper welding
technique.
Description Possible Cause Remedy
1 Excessive bead build-
up or poor
penetration or poor
fusion at edges of
weld.
2 Weld bead too wide
and flat or undercut at
edges of weld or
excessive burn
throu
3 Weld bead too small
or insufficient
penetration or ripples
in bead are widely
s
4 Weld bead too wide or
excessive bead build
up or excessive
penetration in butt
5 Uneven leg length in
fillet joint.
h.
aced apart.
oint.
Welding current is too low. Increase weld current and/or
faulty joint preparation.
Welding current is too high. Decrease weld current.
Travel speed too fast. Reduce travel speed.
Travel speed too slow. Increase travel speed.
Wrong placement of filler rod. Re-position filler rod.
February 22, 2006
Table 10-1: TIG Welding Problems
10-1
Page 54
ARCMASTER 300 ACDC
Description Possible Cause Remedy
6 Electrode melts when
arc is struck.
7 Dirty weld pool. A Electrode contaminated
8 Electrode melts or
oxidizes when an arc
is struck.
9 Poor weld finish. Inadequate shielding gas. Increase gas flow or check
10 Arc flutters during TIG
welding.
A Electrode is connected to
the ‘+’ terminal.
WAVE BALANCE
B
is greater
than 50%.
A Connect the electrode to the
‘-’ terminal.
B Reduced
WAVE BALANCE
to
below 50% or increase the
electrode size.
A Clean the electrode by
through contact with work
piece or filler rod material.
grinding off the
contaminates.
B Gas contaminated with air. B Check gas lines for cuts and
loose fitting or change gas
cylinder.
A No gas flowing to welding
region.
A Check the gas lines for kinks
or breaks and gas cylinder
contents.
B Torch is clogged with dust. B Clean torch.
C Gas hose is cut. C Replace gas hose.
D Gas passage contains
impurities.
D Disconnect gas hose from
torch then raise gas
pressure and blow out
impurities.
E Gas regulator turned off. E Turn on.
F Torch valve is turned off. F Turn on.
G The electrode is too small
for the welding current.
G Increase electrode diameter
or reduce the welding
current.
WAVE BALANCE
H
above 50%.
is set
H Reduced
WAVE BALANCE
below 50% or increase the
to
electrode size.
gas line for gas flow
problems.
A Tungsten electrode is too
large for the welding
current.
B Absence of oxides in the
weld pool.
A Select the right size
electrode. Refer to Basic
TIG Welding guide.
B Refer Basic TIG Welding
Guide for ways to reduce
arc flutter.
Table 10-1 (continued): TIG Welding Problems
10-2
February 22, 2006
Page 55
Description Possible Cause Remedy
11 Welding arc can not
be established.
12 Arc start is not
smooth.
ARCMASTER 300 ACDC
A Work clamp is not
connected to the work piece
or the work/torch leads are
not connected to the right
welding terminals.
B Torch lead is disconnected. B Connect it to the ‘-‘ terminal.
C Gas flow incorrectly set,
cylinder empty or the torch
valve is off.
A Tungsten electrode is too
large for the welding
current.
B The wrong electrode is
being used for the welding
job.
D Incorrect shielding gas is
being used.
E Poor work clamp
connection to work piece.
A Connect the work clamp to
the work piece or connect
the work/torch leads to the
right welding terminals.
C Select the right flow rate,
change cylinders or turn
torch valve on.
A Select the right size
electrode. Refer to Basic
TIG Welding Guide.
B Select the right electrode
type. Refer to Basic TIG
Welding Guide.
Select the correct rate for
CC Gas flow rate is too high.
the welding job.
Refer to Basic TIG Welding
Guide.
D Select the right shielding
gas. Refer to Basic TIG
Welding Guide.
E Improve connection to work
piece.
February 22, 2006
Table 10-1 (continued): TIG Welding Problems
10-3
Page 56
ARCMASTER 300 ACDC
y
p
10.02 Stick Welding Problems
Descri
tion Possible Cause
1 Gas pockets or voids
in weld metal
(Porosity).
2 Crack occurring in
weld metal soon after
solidification
commences.
3 A gap is left by failure
of the weld metal to fill
the root of the weld.
Remed
A Electrodes are damp. A Dry electrodes before use.
B Welding current is too high. B Reduce welding current.
C Surface impurities such as
C Clean joint before welding.
oil, grease, paint, etc.
A Rigidity of joint. A Redesign to relieve weld
joint of severe stresses or
use crack resistance
electrodes.
B Insufficient throat thickness. B Travel slightly slower to
allow greater build up in
throat.
C Cooling rate is too high. C Preheat plate and cool
slowly.
A Welding current is too low. A Increase welding current
B Electrode too large for joint. B Use smaller diameter
electrode.
C Insufficient gap. C Allow wider gap.
D Incorrect sequence. D Use correct build-up
sequence.
Table 10-2: Stick Welding Problems
Art # A-04991
Incorrect sequence
Insufficient
gap
Figure 10-1: Example of insufficient gap or incorrect sequence
10-4
February 22, 2006
Page 57
ARCMASTER 300 ACDC
y
p
Descri
tion Possible Cause
4 Portions of the weld
run do not fuse to the
surface of the metal or
edge of the joint.
Remed
A Small electrodes used on
heavy cold plate.
A Use larger electrodes and
pre-heat the plate.
B Welding current is too low. B Increase welding current.
C Wrong electrode angle. C Adjust angle so the welding
arc is directed more into the
base metal.
D Travel speed of electrode is
too high.
E Scale or dirt on joint
surface.
D Reduce travel speed of
electrode.
E Clean surface before
welding.
Table 10-2 (continued): Stick Welding Problems
Lack of fusion caused by dirt,
Art # A-04992
electrode angle incorrect,
rate of travel too high
Lack of inter-run
fusion
Lack of side fusion, scale
dirt, small electrode,
Lack of root fusion
amperage too low
Figure 10-2: Example of lack of fusion
February 22, 2006
10-5
Page 58
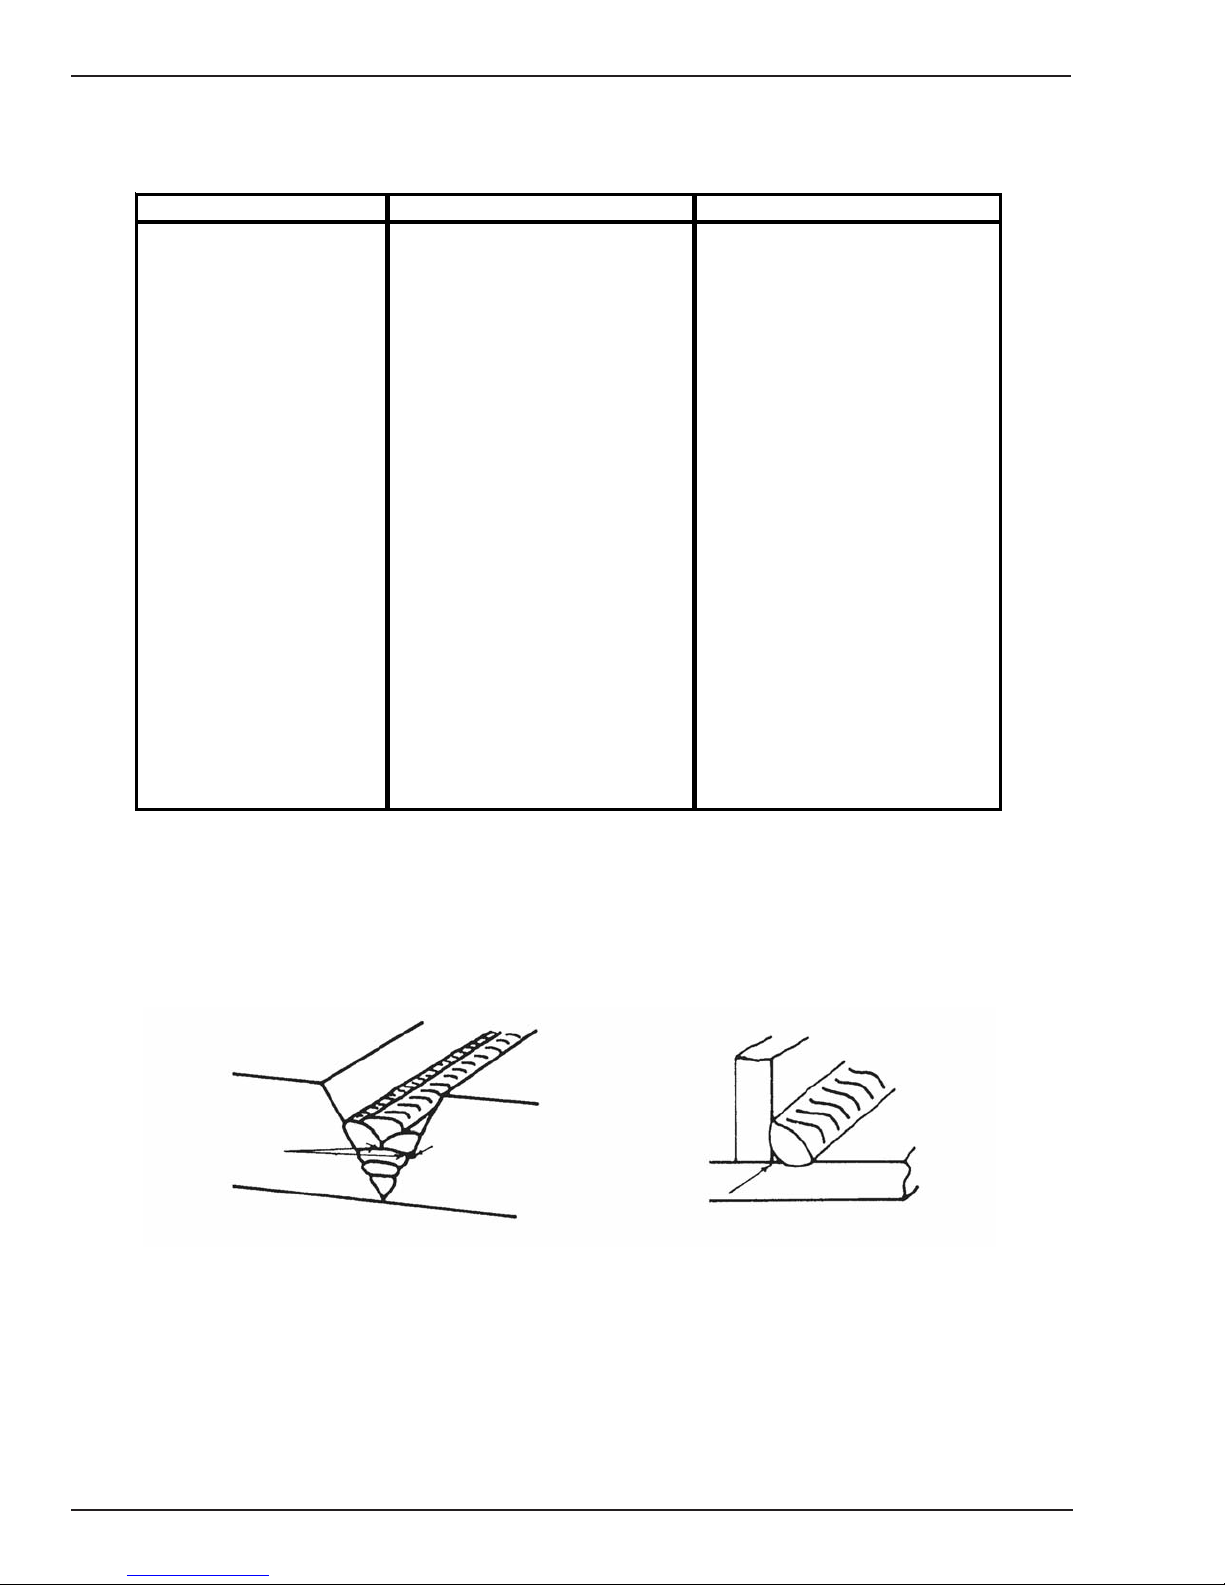
ARCMASTER 300 ACDC
)
g
p
p
y
Descri
tion Possible Cause Remed
5 Non-metallic particles
are trapped in the
weld metal (slag
inclusion
.
A Non-metallic particles may
be trapped in undercut from
previous run.
B Joint preparation too
restricted.
C Irregular deposits allow slag
to be trapped.
D Lack of penetration with
slag trapped beneath weld
bead.
E Rust or mill scale is
reventing full fusion.
F Wrong electrode for position
in which welding is done.
A If bad undercut is present,
clean slag out and cover
with a run from a smaller
diameter electrode.
B Allow for adequate
penetration and room for
cleaning out the slag.
C If very bad, chip or grind
out irregularities.
D Use smaller electrode with
sufficient current to give
adequate penetration. Use
suitable tools to remove all
sla
from corners.
E Clean joint before welding.
F Use electrodes designed for
position in which welding is
done, otherwise proper
control of slag is difficult.
Not cleaned, or
incorrect
electrode
Table 10-2 (continued): Stick Welding Problems
Art # A-04993
Slag trapped in
undercut
Slag trapped in root
Figure 10-3: Examples of slag inclusion
10-6
February 22, 2006
Page 59
10.03 Power Source Problems
Description Possible Cause Remedy
1 The welding arc
cannot be established.
2 Maximum output
welding current can
not be achieved with
nominal Mains supply
voltage.
3 Welding current
reduces when
welding.
4 No gas flow when the
torch trigger switch is
depressed.
ARCMASTER 300 ACDC
A The Primary supply voltage
has not been switched ON.
B The Welding Power Source
switch is switched OFF.
C Loose connections
internally.
Defective control circuit. Have an Accredited Thermal
A Loose welding cable
connections.
B Incorrect welding cable size. B Use proper size and type of
C Improper input connections. C Refer to Section 2.05
D Poor electrode condition. D Replace electrode.
E Wrong welding polarity. E Verify output torch
A Gas hose is cut. A Replace gas hose.
B Gas passage contains
impurities.
C Gas regulator turned off. C Turn gas regulator on.
D Torch trigger switch lead is
disconnected or
switch/cable is faulty.
A Switch ON the Primary
supply voltage.
B Switch ON the Welding
Power Source.
C Have an Accredited Thermal
Arc Service Agent repair the
connection
Arc Service Agent repair the
connection
A Tighten all welding cable
connections.
cable.
Electrical Input
Requirements.
connections.
B Disconnect gas hose from
the rear of Power Source
then raise gas pressure and
blow out impurities.
D Reconnect lead or repair
faulty switch/cable.
February 22, 2006
Table 10-3: Power Source Problems
10-7
Page 60
ARCMASTER 300 ACDC
Description Possible Cause Remedy
5 Gas flow won’t shut
off.
6 The TIG electrode has
been contaminated
due to the gas flow
shutting off before the
programmed
FLOW
time has
elapsed.
POST-
Strike an arc to complete the
A Weld Mode (
REPEAT
changed before
FLOW
finished.
B Gas valve is faulty. B Have an Accredited Thermal
C Gas valve jammed open. C Have an Accredited Thermal
D
POST-FLOW
to 60 sec.
The Weld Process Mode
(STICK, HF TIG or LIFT TIG)
was changed before
FLOW
finished.
STD, SLOPE
or
SPOT
) was
POST-
gas time had
control is set
gas time had
POST-
A
,
D Reduce
weld cycle.
OR
Switch machine off then on
to reset solenoid valve
sequence.
Arc Service Agent repair or
replace the gas valve
Arc Service Agent repair or
replace the gas valve
POST-FLOW
Do not change Weld
Process Mode before the
POST-FLOW
finished.
gas time had
time.
Table 10-3 (continued): Power Source Problems
10-8
February 22, 2006
Page 61
VOLTAGE REDUCTION DEVICE (VRD)
11.01 VRD Specification
Description Notes
VRD Open Circuit Voltage 15.3 to 19.8V Open circuit voltage between welding
VRD Resistance 148 to 193 ohms The required resistance between
VRD Turn OFF Time 0.2 to 0.3
SECTION 11:
ArcMaster
300ACDC
terminals.
welding terminals to turn ON the
welding power.
The time taken to turn OFF the welding
seconds
Table 11-1: VRD Specification
power once the welding current has
stopped.
ARCMASTER 300 ACDC
11.02 VRD Maintenance
Routine inspection and testing (power source):
An inspection of the power source, an insulation resistance test and an earth resistance test should be carried out
a. For transportable equipment, at least once every 3 months;
b. For fixed equipment, at least once every 12 months.
The owners of the equipment shall keep a suitable record of the periodic tests.
NOTE
A transportable power source is any equipment that is not permanently connected and fixed in the position
in which it is operated.
In addition to the above tests and specifically in relation to the VRD fitted to this machine, the following periodic tests
should also be conducted by an accredited Thermal Arc service agent.
Description IEC 60974-1 Requirements
VRD Open Circuit Voltage Less than 20V; at Vin=230V
VRD Turn ON Resistance Less than 200 ohms
VRD Turn OFF Time Less than 0.3 seconds
Table 11-2: Periodic Tests
If this equipment is used in a location or an environment with a high risk of electrocution then the above tests should
be carried out prior to entering this location.
February 22, 2006
11-1
Page 62
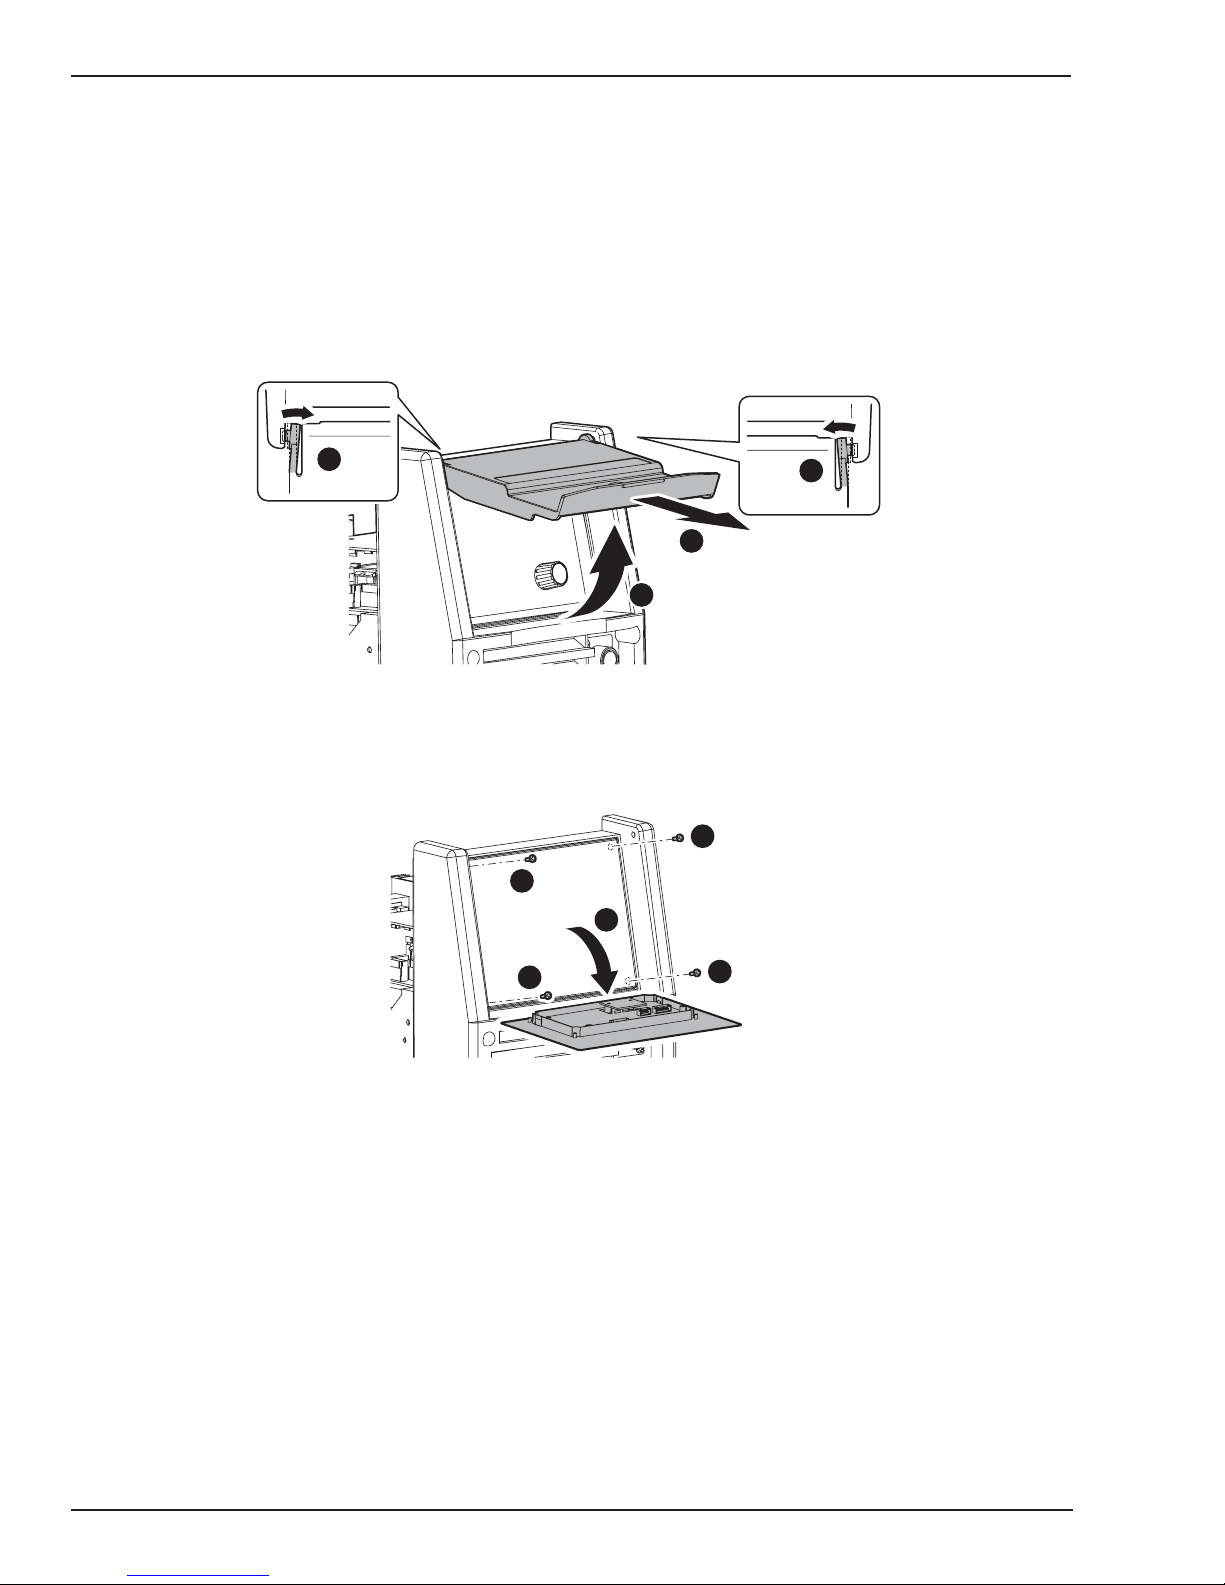
ARCMASTER 300 ACDC
11.03 Switching VRD On/Off
Switch the machine Off.
A) Remove the clear plastic cover from the control panel (see Figure 11-1).
• Lift up the cover so it rests on the top of the unit
• Place a small flat bladed screw driver between the cover hinge on the front panel
• Gently lift the cover hinge out of the front cover mounting hole
• Remove the control's clear plastic cover
2
3
1
2
Art # A-07079
Figure 11-1: VRD ON/OFF Step A
B) Remove the four mounting screws from the the control panel (see Figure 11-2).
Art # A-07080
1
2
1
1
1
11-2
Figure 11-2: VRD ON/OFF Step B
February 22, 2006
Page 63
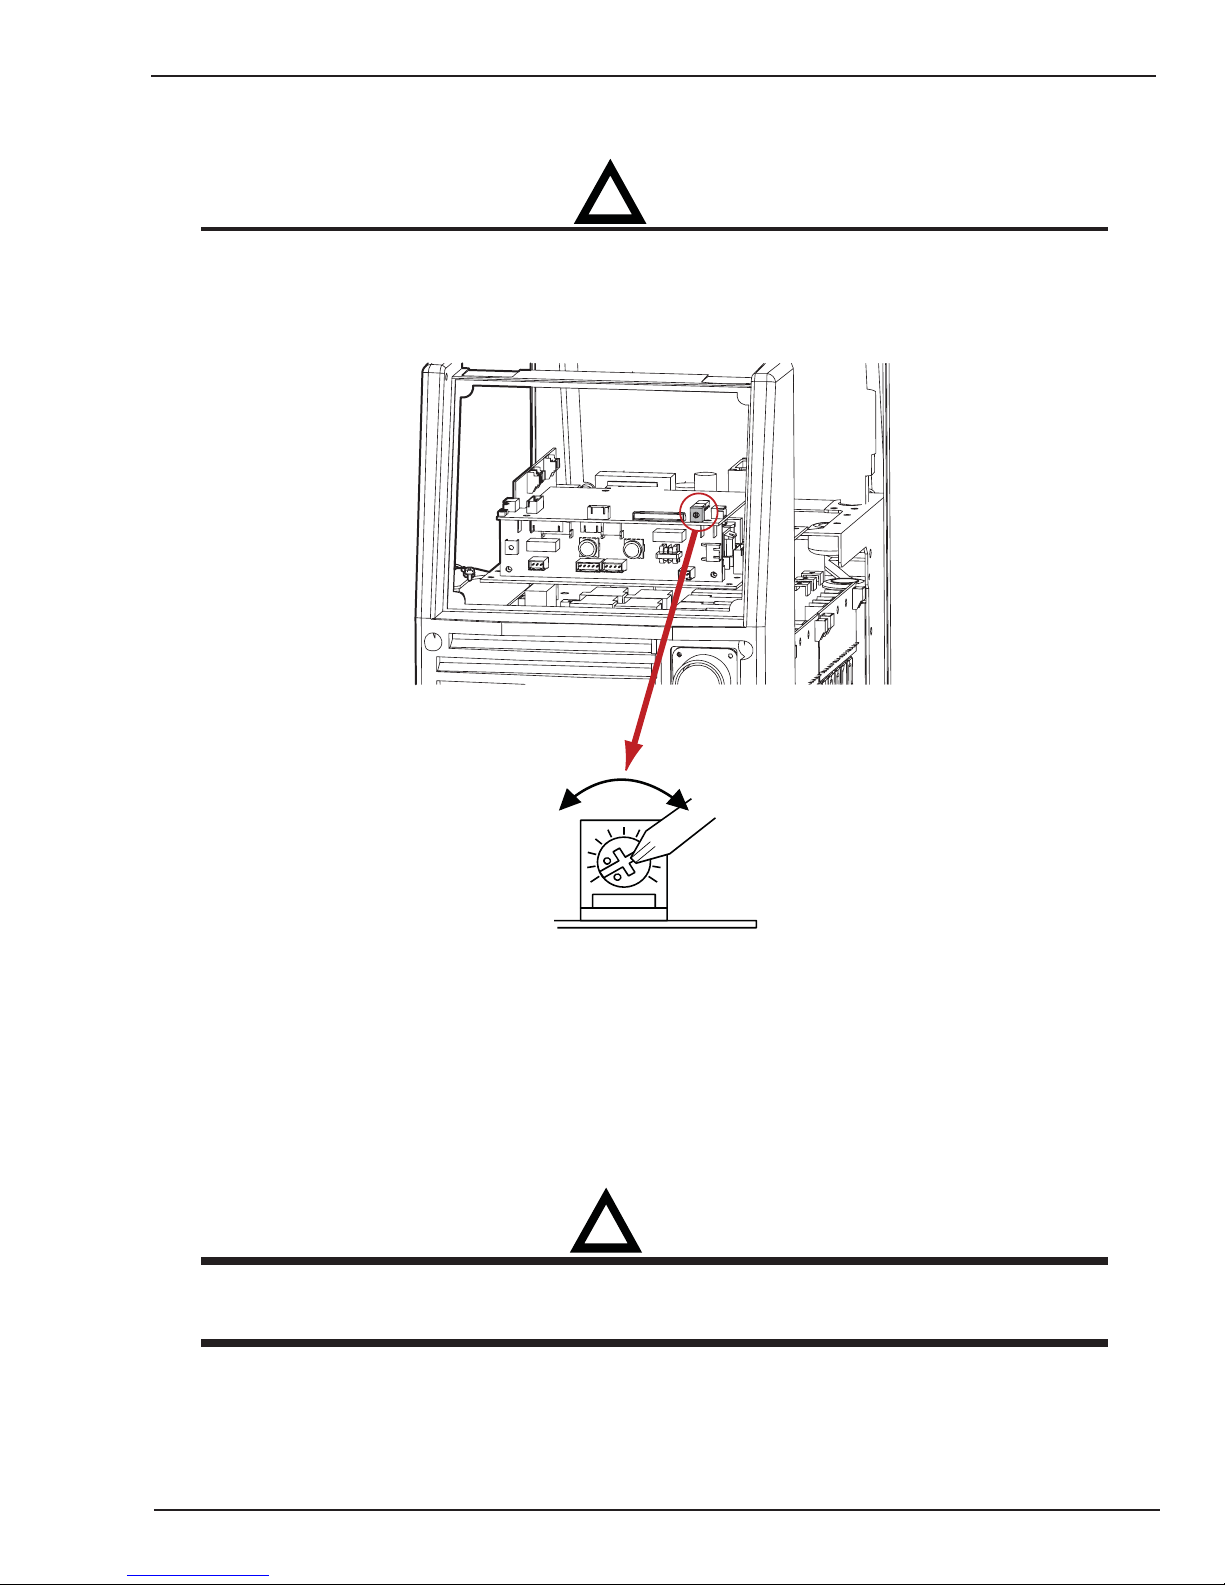
ARCMASTER 300 ACDC
!
!
C) Access the VRD control by gently prying back the front panel controls to reveal the VRD on/off potentiometer (see
Figure 11-3).
CAUTION
DO NOT pull back the front panel with excessive force as this will unplug control PCB. Plugging the control
PCB back into the front panel controls can only be achieved by removing the side covers.
VR1
Art # A-07081
Figure 11-3: VRD ON/OFF Step C and D
D) Turning the VRD ON/OFF (see Figure 11-3)
• To turn VRD ON: rotate the trim potentiometer on the display PCB fully clockwise. When VRD is turned ON check
that it operates as per VRD Specifications on page 11-1.
• To turn VRD OFF: rotate the trim potentiometer on the display PCB fully counter clockwise.
WARNING
The VRD ON/OFF trim potentiometer MUST ONLY be positioned fully clockwise OR fully counter clockwise
as the VRD function will be unknown for every other position.
February 22, 2006
11-3
Page 64
ARCMASTER 300 ACDC
11-4
February 22, 2006
Page 65
SECTION 12:
POWER SOURCE ERROR CODES
Description Possible Cause Remedy Remarks
1 E01 error code
displayed
Temperature sensor
TH1 (protects
IGBTs) is greater
than 80ºC for about
1 second.
2 E02 error code
displayed
Temperature sensor
TH2 (protects
secondary diodes)
is greater than 80ºC
for about 1 second.
3 E03 error code
displayed
Primary (input)
current too high.
E04 error code
4 TIG torch cable
displayed
Output voltage
exceeds the
secondary voltage
specification.
A The Welding Power
Source’s duty cycle
has been exceeded.
B Fan ceases to
operate.
C Air flow is restricted
by vents being
blocked.
A The Welding Power
Source’s duty cycle
has been exceeded.
B Fan ceases to
operate.
C Air flow is restricted
by vents being
blocked.
A Primary current is
too high because
welding arc is too
long.
B Mains supply
voltage is more than
10% below nominal
voltage .
and/or work lead are
too long or leads
are coiled.
ARCMASTER 300 ACDCR
A Let Power Source
cool down then
keep within its duty
cycle.
B Have an Accredited
Thermal Arc Service
Agent investigate.
C Unblock vents then
let Power Source
cool down.
A Let Power Source
cool down then
keep within its duty
cycle.
B Have an Accredited
Thermal Arc Service
Agent investigate
C Unblock vents then
let Power Source
cool down.
A Reduce length of
welding arc.
B Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check for
low Mains voltage.
Reduce the length
of the TIG torch
cable and/or work
lead or un-coiled
leads.
Weld current
ceases. Buzzer
sounds constantly.
Fan operates at max
speed.
E01 resets when
TH1 decreases to
70ºC for about 30
seconds.
Weld current
ceases. Buzzer
sounds constantly.
Fan operates at max
speed.
E02 resets when
TH2 decreases to
70ºC for about 30
seconds.
Weld current
ceases. Buzzer
sounds constantly.
Fan operates at max
speed.
Switch machine off
then on to reset E03
error.
Weld current
ceases. Buzzer
sounds constantly.
Switch machine off
then on to reset E04
error.
February 22, 2006
Table 12-1 Power Source Error Codes
12-1
Page 66
ARCMASTER 300 ACDC
E11 error code
5 Primary supply
displayed
Over Primary supply
(input) voltage at
voltage is greater
than the nominal
voltage plus 10%.
primary capacitors
is exceeded for one
second.
E14 error code
6
displayed
Under mains supply
(input) voltage
warning primary
Mains supply
voltage is less than
the nominal
operating voltage
less 10%.
capacitors is
reduced for one
second.
7 Mains supply
E12 error code
displayed
Under mains supply
(input) voltage
voltage is down to a
dangerously low
level.
primary capacitors
is reduced for one
second.
E81 error code
8 When 3 phase
displayed
Wrong Primary
supply (input)
voltage connected.
machine is first
turned on with the
wrong Primary
supply (input)
voltage connected.
Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
Primary voltage.
Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
Mains voltage.
A Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
Mains voltage.
B Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
primary cable and
fuses.
Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
Mains voltage.
Weld current
ceases. Buzzer
sounds contstantly.
Error code E11
automatically will
reset when the
voltage reduces.
Weld current
available. Buzzer
sounds
intermittently.
Error code E14
automatically will
reset when the
voltage increases.
Weld current
ceases. Buzzer
sounds contstantly.
Error code E12
automatically will
reset when the
voltage increases.
No weld current is
available. Buzzer
sounds constantly.
Switch machine off.
Table 12-1 (continued): Power Source Error Codes
12-2
February 22, 2006
Page 67
ARCMASTER 300 ACDCR
E82 error code
9 The Primary supply
displayed
Rated voltage
selection circuit
(input) voltage
fluctuates and is not
stable.
abnormality.
E83 error code
10 The Primary supply
displayed
CPU checks mains
supply (input)
(input) voltage
fluctuates and is not
stable.
voltage when the
on/off switch on
rear panel of
machine is turned
ON.
E85 error code
11
displayed
Pre-charge
abnormality.
Due to malfunction
inside the Welding
Power Source,
primary capacitors
are not charging
E93 error code
12 Memory chip
displayed
(EEPROM) error.
Memory chip
(EEPROM) on
control PCB can not
read/write weld
parameters.
Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
Mains voltage.
Have an Accredited
Thermal Arc Service
Agent check
connector plug on
input PCB and the
Mains voltage
Have an Accredited
Thermal Arc Service
Agent service the
machine
Have an Accredited
Thermal Arc Service
Agent check the
control PCB.
No weld current is
available. Buzzer
sounds constantly.
Switch machine off
then on to reset E82
No weld current is
available. Buzzer
sounds constantly.
Switch machine off
then on to reset E83
error.
No weld current is
available. Buzzer
sounds constantly.
Switch machine off
then on to reset E85
Weld current
ceases. Buzzer
sounds constantly.
Switch machine off.
February 22, 2006
Table 12-1 (continued): Power Source Error Codes
12-3
Page 68
ARCMASTER 300 ACDC
E94 error code
13 The Welding Power
displayed
Temperature sensor
TH1 for IGBTs or
sensor TH2 for
Source’s
temperature
sensors have
malfunctioned.
secondary diodes
Have an Accredited
Thermal Arc Service
Agent check or
replace the
temperature
sensors
Weld current
ceases. Buzzer
sounds constantly.
Switch machine off.
are open circuit.
E99 error code
14 Weld current
displayed
A Main on/off switch
on machine has
been turned off
Mains supply
(input) voltage has
been turned off but
Mains supply
(input) voltage has
been turned off.
control circuit has
power from the
primary capacitors.
Table 12-1 (continued): Power Source Error Codes
A Turn on/off switch
on.
B Have an Accredited
Thermal Arc Service
Agent or a qualified
electrician check the
Mains voltage and
fuses.
ceases. Buzzer
sounds constantly.
Must switch
machine off then on
to reset E99 error.
12-4
February 22, 2006
Page 69
SECTION 13:
PARTS LIST
ARCMASTER 300 ACDC
13.01 Equipment Identification
All identification numbers as described in the Introduction chapter must be furnished when ordering parts or
making inquiries. This information is usually found on the
nameplate attached to the equipment. Be sure to include
any dash numbers following the Specification or Assembly numbers.
13.02 How To Use This Parts List
The Parts List is a combination of an illustration and a
corresponding list of parts which contains a breakdown
of the equipment into assemblies, subassemblies, and
detail parts. All parts of the equipment are listed except
for commercially available hardware, bulk items such as
wire, cable, sleeving, tubing, etc., and permanently attached items which are soldered, riveted, or welded to
other parts. The part descriptions may be indented to show
part relationships.
To determine the part number, description, quantity, or
application of an item, simply locate the item in question
from the illustration and refer to that item number in the
corresponding Parts List.
PART NUMBER:
ArcMaster 300 ACDC 10-3074
February 22, 2006
13-1
Page 70
ARCMASTER 300 ACDC
DWG. No. Description Type & Rating QTY. Code No. Order No.
C1 Capacitor ECQE12104MZ
CC1 Coupling Coil F2A636900 185A
CON1 Remote
Socket
D1 Diode DFA50BA160 1 454160160 10-6628
D2 Diode DBA200UA60 1 4583A0060 10-6629
D4 Diode DBA200UA60 1 4583A0060 10-6629
D5 Diode DBA200UA60 1 4583A0060 10-6629
D10 Diode S2VB60 600V 1 444014023 10-6630
FAN1 Fan 109E5724H507
FCH1 Inductor F2A676800 185A
HCT1 Current
Sensor
HF.UNIT 1 HF. Unit HF.UNIT (WK-
HF. Gap U0A601100 1 U0A601100 10-6633
L105 Inductor 1615MRE RING
PCB1 Printed Circuit
Board
PCB2 Printed Circuit
Board
PCB3 Printed Circuit
Board
PCB4 Printed Circuit
Board
PCB5 Printed Circuit
Board
PCB6 Printed Circuit
Board
DC1250V 0.1uF
CC
-
(with Wiring
Assembly)
DC 24V 16.8W
AC/DC FCH
HCTN200V4B15M
200A 4V
4840 U02)
CORE
WK-4914 U04
MAIN_PCB (with
Insulation Sheet
EBA501500) with
Thunder Label
WK-4819 U01
DETECT PCB
WK-4921 U02
CONNECT PCB
WK-4915 U04 2
DIODE with
Thunder Label
WK-4916 U02 2IGBT PCB
WK-5157 U11
TIG CONTROL
1 42422137100 10-2270
1 F2A636900 10-6626
1 U0A706100
1 U0A733500 10-6839
1 F2A676800 10-6631
1 11251003000 10-5003
1 U0A632200 10-6632
1 63200006500 10-6538
1 U0A705100 10-6634
1 P0A481901 10-6635
1 P0A492102 10-6636
ND
1 U0A705200
1 P0A491602 10-6638
1 P0A515711 10-6846
10-6627
10-6637
13-2
February 22, 2006
Page 71
ARCMASTER 300 ACDC
)
DWG. No. Description Type & Rating QTY. Code No. Order No.
PCB7 Printed Circuit
Board
PCB8 Printed Circuit
Board
Q1 Transistor 1 U0A705300
Q2 Transistor 1 U0A705400 10-6643
R1 Resistor (For
HF Unit)
R2 Resistor JG23V101J 68W
S1 Switch DCP-52SR50C-
Valve
T1 Transformer F2A708300 250A
T2 Transformer F2A708300 250A
T3 Transformer F2A758000
TH1,2 Thermistor ERTA53D203
Front Panel E0D005300 1 E0D005300 10-6890
Rear Panel E0D005500 1 E0D005500 10-6891
Side Panel E0D006100 2 E0D006100 10-6650
Front Control
Cover
Rear Control
Cover
Protection
Cover
WK-4920 U10 AC
1 P0A492010 10-6640
TIG PANEL
WK-4917 U06
1 P0A491706 10-6641
FILTER 240V
CM100DUS12F-1
10-6642
600V 100A
(with WK-5012
U01)
GCA200CA60
(with WK-3367
U04)
ERF20HMJ151
1 40310211500 10-5081
20W 150 W
2 40511000200 10-5137
100 W
1 25850003500 10-6644
480V 2P-480V
5505NBR1.5
1 U0A705700
10-6645SOL1 Solenoid
DC24V 11VA/10W
(with Gas Inlet
and PC4-02)
1 F2A708300 10-6646
MTR
1 F2A708300 10-6646
MTR
1 F2A758000 10-6647
AC/DC DTR
1 U0A733300 10-6784
20K"/25ºC
B=3950K
J4B493400 1 J4B493400 10-6651
JCA849400 (with
1 U0A705500 10-6652
Label
E0C303200 1 E0C303200 10-6653
February 22, 2006
13-3
Page 72
ARCMASTER 300 ACDC
DWG. No. Description Type & Rating QTY. Code No. Order No.
Encoder
Cover
PCB Cover E1B537600 (with
Name Label N4A007600 2 N4A007600 10-6656
“VRD INSIDE”
Label
VRD Caution
Label
Primary
Power HookUp Label
Side Label N4A009200 2 N4A009200 10-6657
Warning 1
Label
Warning 2
Label
Output
Terminal
Label
Gas Outlet EBA077600 (with
C-Ring 2 53003000600 10-5184
Output
Terminal
(female)
Input Cable 132” 10/3 SOW
Input Cable
Clamp
Heatsink E1B538500 1 E1B538500 10-6663
Heatsink E1B538600 1 E1B538600 10-6664
Knob 2621603 1 50990001600 10-6665
Knob Cap 3021104 1 50990000300 10-6666
Control Cover
Sheet
Flat Cable EAA547301 1 EAA547301 10-6668
Post1(M4M5)
EBA514400 1 EBA514400 10-6654
1 U0A705600 10-6655
Caution Label)
N4A155900 1 N4A155900 Ref. Only
N4A598700 1 N4A598700 23X4915
N4A598200 1 N4A598200 23X4914
N0B891300 1 N0B891300 10-5497
N0B476400 2 N0B476400 10-5496
N4A040100 1 N4A040100 10-6658
1 U0A705800 10-6659
PC4-02)
TRAK-BE35-70S 2 26999025900 10-6660
1 52031130000 10-6844
BLK W/6-50P
EBA045800 1 EBA045800 10-6662
N0B882200 1 N0B882200 10-6667
EBA424900 2 EBA424900 10-6669
13-4
February 22, 2006
Page 73
ARCMASTER 300 ACDC
DWG. No. Description Type & Rating QTY. Code No. Order No.
Post4(M4M4)
Post5(M4M4)
Post6(M5M5)
Post7(M5M5)
Post8(M5M5)
D2-4 Bus Bar EBA305600 2 EBA305600 10-6675
CC Bus Bar EBA306200 1 EBA306200 10-6676
S1 Bus Bar ECA321000 2 ECA321000 10-6868
Clip #74 NATURAL
Transformer
Chassis
Right Chassis J2C970700 1 J2C970700 10-6679
Left Chassis J2C970800 1 J2C970800 10-6680
Nylon Hose T0425B Nylon
Output
Terminal
(male)
Operators
Manual
Service
Manual
EBA431100 3 EBA431100 10-6670
EBA431200 6 EBA431200 10-6671
EBA431300 1 EBA431300 10-6672
EBA435900 3 EBA435900 10-6673
EBA436000 3 EBA436000 10-6674
4 60602422000 10-5259
(Plastic Tab)
JCA903200 1 JCA903200 10-6678
1 U0A706000 10-6681
Hose L=0.5m
TRAK-SK50 2 26999025800 10-2020
1 430429-503
430429-512
February 22, 2006
13-5
Page 74
ARCMASTER 300 ACDC
13-6
February 22, 2006
Page 75
Page 76
LIMITED WARRANTY
y
r
t
f
f
r
y
y
This information applies to Thermal Arc products that were purchased in the USA and Canada.
April 2006
LIMITED WARRANTY: Thermal Arc
®
, Inc., A Thermadyne Company ("Thermal Arc"),
warrants to customers of authorized distributors ("Purcha ser") that its products will be free
of defects in workmanship or material. Should any failure to conform to this warrant
appear within the warranty period stated below, Thermal Arc shall, upon notification
thereof and substantiation that the product has been stored, installed, operated, and
maintained in accordance with Thermal Arc's specifications, instructions,
recommendat ions and recognized stan dard industry practic e, and not subject to misu se,
repair, neglect, alteration, or damage, correct such defects by suitable repair o
replacement, at Thermal Arc's sole option, of any components or parts of the produc
determined by Thermal Arc to be defective.
This warranty is exclusive and in lieu of any warranty o
merchantability, fitness for any particular purpose, or other warranty o
quality, whether express, implied, or statutory.
Limitation of liability: Therma l Arc shall not under an y circumstances be lia ble for special,
indirect, incidental, or consequential damages, including but not limited to lost profits and
business interruption. The remedies of the purchaser set forth herein are exclusive, and
the liability of Thermal A rc with respect to any co ntract, or anything done in connection
therewith such as the performance or breach thereof, or from the manufacture, sale,
delivery, resale, or use of any goods covered by or furnished by Thermal Arc, whethe
arising out of contract, tort, in cluding negligence or strict liability, or under any warranty,
or otherwise, shall not exceed the price of the goods upon which such liability is based.
No employee, agent, or representative of Thermal Arc is authorized to change this
warranty in any way or grant any other warranty, and Thermal Arc shall not be bound b
any such attempt. Correction of non-conformities, in the manner and time provided
herein, constitutes fulfillment of thermal’s obligations to purchaser with respect to the
product.
This warranty is void, and seller bears no liability hereunder, if purchaser used
replacement parts or accessories which, in Thermal Arc's sole judgment, impaired the
safety or performance of any Therma l Arc product. Purchaser’s r i ghts under this warrant
are void if the product is sold to purchaser by unauthorized p ersons.
The warranty is effective for the time stated below beginning on the date that the
authorized distributor delivers the products to the Purchaser. Notwithstanding the
foregoing, in no event shall the warranty period extend more than the time stated plus
one year from the date Thermal Arc delivered the product to the authorized distributor.
Warranty repairs or replacement claims under this limited warranty must be submitted to
Thermal Arc via an authorized Thermal Arc repair facility within thirty (30) days of
purchaser's discovery of any defect. Thermal Arc shall pay no transportation costs of any
kind under this warranty. Transportation charges to send products to an authorized
warranty repair facility shall be the responsibility of the Purchaser . All returned goods
shall be at the Purchaser's risk and expense. This warranty dated April 1
®
supersedes all previous Thermal Arc warranties. Thermal Arc
is a Registered
st
2006
Trademark of Thermal Arc, Inc.
Page 77
WARRANTY SCHEDULE
This information applies to Thermal Arc products that were purchased in the USA and Canada.
April 2006
ENGINE DRIVEN WELDERS WARRANTY PERIOD LABOR
Scout, Raider, Explorer
Original Main Power Stators and Inductors .................................................................................. 3 years
Original Main Power Rectifiers, Control P.C. Boards................................................................... 3 years
All other original circuits and components including, but not limited to, relays,
switches, contactors, solenoids, fans, power switch semi-conductors..........................................1 year
Engines and associated components are NOT warranted by Thermal Arc, although
most are warranted by the engine manufacturer............................................................. See the Engine’s Warranty for Details
GMAW/FCAW (MIG) WELDING EQUIPMENT WARRANTY PERIOD LABOR
Fabricator 131, 181; 190, 210, 251, 281; Fabstar 4030;
PowerMaster 350, 350P, 500, 500P; Excelarc 6045.
Wire Feeders; Ultrafeed, Portafeed
Original Main Power Transformer and Inductor............................................................................5 years 3 years
Original Main Power Rectifiers, Control P.C. Boards, power switch semi-conductors................. 3 years 3 years
All other original circuits and components including, but not limited to, relays,
switches, contactors, solenoids, fans, electric motors...................................................................1 year
GTAW (TIG) & MULTI-PROCESS INVERTER WELDING EQUIPMENT WARRANTY PERIOD LABOR
160TS, 300TS, 400TS, 185AC/DC, 200AC/DC, 300A C/ DC, 400GT S W, 400MST,
300MST, 400MSTP
Original Main Power Magnetics....................................................................................................5 years 3 years
Original Main Power Rectifiers, Control P.C. Boards, power switch semi-conductors................. 3 years 3 years
All other original circuits and components including, but not limited to, relays,
switches, contactors, solenoids, fans, electric motors...................................................................1 year
PLASMA WELDING EQUIPMENT WARRANTY PERIOD LABOR
Ultima 150
Original Main Power Magnetics.................................................................................................... 5 years 3 years
Original Main Power Rectifiers, Control P.C. Boards, power switch semi-conductors................. 3 years 3 years
Welding Console, Weld Controller, Weld Timer ........................................................................... 3 years 3 years
All other original circuits and components including, but not limited to, relays,
switches, contactors, solenoids, fans, electric motors, Coolant Recirculator................................1 year
SMAW (Stick) WELDING EQUIPMENT WARRANTY PERIOD LABOR
Dragster 85
Original Main Power Magnetics.....................................................................................................1 year 1 year
Original Main Power Rectifiers, Control P.C. Boards....................................................................1 year 1 y ear
All other original circuits and components including, but not limited to, relays,
switches, contactors, solenoids, fans, power switch semi-conductors..........................................1 year
160S, 300S, 400S
Original Main Power Magnetics....................................................................................................5 years 3 years
Original Main Po w e r Rect ifiers, Control P .C . B o ards .. ............................................................... .. 3 years 3 years
All other original circuits and components including, but not limited to, relays,
switches, contactors, solenoids, fans, power switch semi-conductors..........................................1 year
GENERAL ARC EQUIPMENT WARRANTY PERIOD LABOR
Water Recirculators.......................................................................................................................1 year 1 year
Plasma Welding Torches............................................................................................................. 180 days 180 days
Gas Regulators (Supplied with power sources)..........................................................................180 days Nil
MIG and TIG Torches (Supplied with power sources)..................................................................90 days Nil
Replacement repair parts.............................................................................................................90 days Nil
MIG, TIG and Plasma welding torch consumable items...................................................................Nil Nil
3 years
3 years
1 year
1 year
1 year
1 year
1 year
1 year
Page 78
Page 79
GLOBAL CUSTOMER SERVICE CONTACT INFORMATION
Thermadyne USA
2800 Airport Road
Denton, Tx 76207 USA
Telephone: (940) 566-2000
800-426-1888
Fax: 800-535-0557
Email: [email protected]
Thermadyne Canada
2070 Wyecroft Road
Oakville, Ontario
Canada, L6L5V6
Telephone: (905)-827-1111
Fax: 905-827-3648
Thermadyne Europe
Europe Building
Chorley North Industrial Park
Chorley, Lancashire
England, PR6 7Bx
Telephone: 44-1257-261755
Fax: 44-1257-224800
Thermadyne Asia Sdn Bhd
Lot 151, Jalan Industri 3/5A
Rawang Integrated Industrial Park - Jln Batu Arang
48000 Rawang Selangor Darul Ehsan
West Malaysia
Telephone: 603+ 6092 2988
Fax : 603+ 6092 1085
Cigweld, Australia
71 Gower Street
Preston, Victoria
Australia, 3072
Telephone: 61-3-9474-7400
Fax: 61-3-9474-7510
Thermadyne Italy
OCIM, S.r.L.
Via Benaco, 3
20098 S. Giuliano
Milan, Italy
Tel: (39) 02-98 80320
Fax: (39) 02-98 281773
Thermadyne, China
RM 102A
685 Ding Xi Rd
Chang Ning District
Shanghai, PR, 200052
Telephone: 86-21-69171135
Fax: 86-21-69171139
Thermadyne International
2070 Wyecroft Road
Oakville, Ontario
Canada, L6L5V6
Telephone: (905)-827-9777
Fax: 905-827-9797
Page 80
World Headquarters
Thermadyne Holdings Corporation
Suite 300, 16052 Swingley Ridge Road
St. Louis, MO 63017
Telephone: (636) 728-3000
Fascimile: (636) 728-3010
Email: sales@thermalarc.com
www.thermalarc.com
 Loading...