

Page 1

D E C 0 0 2 / 0 4
TAILIFT LTD. 2006
RADIAL DRILLS
TPR720A TPR820A
TPR920A TPR1100
Operation Manual
Page 2

1-1
CHAPTR 1
Safety Guidelines
1.1 Please follow the below basic safety principles﹕﹕﹕﹕
(1) Have only sophisticated or experienced personal perform the machine operation or
maintenance.
(2) Please read and understand the operation manual thoroughly before operation.
(3)
Please place the manual close to the machine for easy access.
(4) Please have only authorized person keep the keys to the machine.
(5)
All operation and maintenance personnel need to know the location of the emergency
switch, its function and operation.
1.2 Precautions for the transportation and installation.
(1) Please make sure that the floor is solid enough to support the machine.
(2) Only one person is allowed to lift and move the machine for safety reason.
(3) When lifting and moving, Nobody is allowed to be under or near the machine.
(4) Please wear protective helmet when moving, installing or clearing the machine.
(5) All levers, which tighten, need to be tightened.
(6) If the moving object weighs over 25kgs, Please use on
ly proper movement equipment
for it.
(7) Please make sure that the slings are strong enough to lift the machine or the subjects.
(8)
Please power off before movement and installation. If necessary to power on, please
let other persons know the location of the emergent stop.
(9)
Please put on leather gloves or similar protective equipments when moving,
installing or clearing the machine.
Page 3

1-2
1.3 Precautions for operation:
(1) Please don’t remove any protection guard or any safety installation.
(2) Please don’t remove or alter any location of the limit switches, restraint blocks or
interlocking mechanisms.
(3) Don’t touch any switch with wet hand.
(4) Please don’t put any part of your body on the moving parts of the machine or near
to them.
(5) The operation person have better no long hair, if it is impossible, please have it
coiled in a topknot and wear a safety helmet.
(6) Please wear no hand ring, watch, pearls or loose clothes. Operation should wear a
safety clothes.
(7) Please wear no slippery shoes while operating.
(8) Wearing gloves is needed when loading and unloading material.
(9) Only one person is allowed to operate the machine.
(10) While operation, Debris may fly off. So please wear a protective mask to prevent
from being injured.
(11) Please power off after work.
(12) Please wear a gauze mask if you are working, using cutting fluids.
(13) Please don’t use the machine in a explosive environment.
(14) A risk of being squeezed is composed when the gearbox and the arm are d
escending
or the spindle is descending to the worktable. (The arm screw moves at a low speed
of 0.8 m/min.)
(15)
Operator should stand in front of the machine. That’s the operation position.
1.4 Precautions for checking and maintenance.
(1) Please power off first before performing maintenance or checking job.
(2) Only have authorized electric technician carry out maintenance or checking job
when Power-on is needed in it
(3) Please power off after work.
(4) Adding or replacing hydraulic oil or lubricant, Please use Tailift recommended oil
type or its equivalent. For details, please refer to the chapter 7.
(5) Basically, only one person is needed to serve. If more than one person is called for,
Good communications is required.
(6) Please power off first before getting rid of the iron filings or cleaning the machine.
Page 4

1-3
1.5 Warning labels and mark on the machine
1.5.1 Warning labels and mark introduction
labels Description
Please secure the machine with the base
fixing bolts, to prevent from any risk.
台勵福股份有限公司
台品工業股份有限公司
TAI PIN INDUSTRIAL CO., LTD
機型號碼
機型號碼機型號碼
機型號碼
MODEL NO.
MODEL NO.MODEL NO.
MODEL NO.
製造日期
製造日期製造日期
製造日期
MFG.DATE
MFG.DATEMFG.DATE
MFG.DATE
機台重量
機台重量機台重量
機台重量
NET WEIGHT
NET WEIGHTNET WEIGHT
NET WEIGHT
製造號碼
製造號碼製造號碼
製造號碼
SERIAL NO.
SERIAL NO.SERIAL NO.
SERIAL NO.
電源供應量
電源供應量電源供應量
電源供應量
POWER SUPPLY
POWER SUPPLYP OWER SUPPLY
POWER SUPPLY
kva
通訊地 址
通訊地 址通訊地 址
通訊地 址:台 中縣大雅 鄉員林村 神林路
台中 縣大雅鄉 員林村神林 路台中 縣大雅鄉 員林村神林 路
台中 縣大雅鄉 員林村神林 路1段段段段26 9號號號號
NO. 2 69 S EC .1 , S HEI N LI N RD . , YU AN LI N TS UN ,
NO. 2 69 S EC .1 , S HEI N LI N RD . , YU AN LI N TS UN ,NO. 2 69 S EC .1 , S HEI N LI N RD . , YU AN LI N TS UN ,
NO. 2 69 S EC .1 , S HEI N LI N RD . , YU AN LI N TS UN ,
TA YA H SI AN G , TA IC HU NG H SI EN , T AI WAN .
TA YA H SI AN G , TA IC HU NG H SI EN , T AI WAN .TA YA H SI AN G , TA IC HU NG H SI EN , T AI WAN .
TA YA H SI AN G , TA IC HU NG H SI EN , T AI WAN .
TEL :886 -4-2 5666 100 FAX: 886- 4-25 6716 70
TEL :886 -4-2 5666 100 FAX: 886- 4-25 6716 70TEL :886 -4-2 5666 100 FAX: 886- 4-25 6716 70
TEL :886 -4-2 5666 100 FAX: 886- 4-25 6716 70
kg
Model of a machine.
Please watch out the running tools.
Please operat
ors wear a protective glasses
during work.
CE Mark
(
((
(option))))
Oil filler position.
Oil drain outlet position.
Risk of high voltage....
Page 5

1-4
1.5.2 Warning Labels and mark positions
a. The front view.
b-1. The rear view (For TPR-720A, TPR-820A, TPR-920A)
台勵福股份有限公司
台品工業股份有限公司
TAI PIN INDUSTRIAL CO., LTD
機型號碼
機型號碼機型號碼
機型號碼
MODEL NO.
MODEL NO.MODEL NO.
MODEL NO.
製造日期
製造日期製造日期
製造日期
MFG.DATE
MFG.DATEMFG.DATE
MFG.DATE
機台重量
機台重量機台重量
機台重量
NET WEIGHT
NET WEIGHTNET WEIGHT
NET WEIGHT
製造號碼
製造號碼製造號碼
製造號碼
SERIAL NO.
SERIAL NO.SERIAL NO.
SERIAL NO.
電源供應量
電源供應量電源供應量
電源供應量
POWER SUPPLY
POWER SUPPLYPOWER SUPPLY
POWER SUPPLY
kva
通訊 地址
通訊 地址通訊地 址
通訊 地址 :台中 縣大 雅鄉 員林 村神林路
台中 縣大 雅鄉員林 村神 林路台中 縣大 雅鄉員林 村神 林路
台中 縣大 雅鄉員林 村神 林路1 段段段段26 9號號號號
NO. 2 69 S EC .1 , S HE IN L IN R D. , Y UAN L IN T SU N ,
NO. 2 69 S EC .1 , S HE IN L IN R D. , Y UAN L IN T SU N ,NO. 2 69 S EC .1 , S HE IN L IN R D. , Y UAN L IN T SU N ,
NO. 2 69 S EC .1 , S HE IN L IN R D. , Y UAN L IN T SU N ,
TA YA H SI AN G , T AI CH UN G HS IE N , T AI WA N.
TA YA H SI AN G , T AI CH UN G HS IE N , T AI WA N.TA YA H SI AN G , T AI CH UN G HS IEN , T AI WA N.
TA YA H SI AN G , T AI CH UN G HS IE N , T AI WA N.
TE L: 886- 4-25 6661 00 FAX :886 -4-2 5671 670
TE L: 886- 4-25 6661 00 FAX :886 -4-2 5671 670TE L: 886- 4- 2566 6100 FAX :886 -4-2 5671 670
TE L: 886- 4-25 6661 00 FAX :886 -4-2 5671 670
kg
Page 6

1-5
b-2. The rear view (only for TPR-1100)
C. Oil filler position and Oil Drain outlet position
Gearbox
Page 7

1-6
Arm elevating motor (For TPR-720A, TPR-820A, TPR-920A)
Arm elevating motor (For TPR-1100)
Page 8

2-1
CHAPTER 2
General Specifications
2.1 The anticipated machine life.
The calculation of the anticipated machine life:
8 hours x 6 days x 50 weeks x 10 years = 24000 hours.
The above calculation is based on a sound maintenance and normal condition,
excluding wearing parts.
2.2 Machine dimensions.
The following are the machines’ dimensions and its diagrams.
Models A B C
TPR-720A 1250mm 640mm 2170mm
TPR-820A 1250mm 640mm 2320mm
TPR-920A 1250mm 640mm 2320mm
TPR-1100 1710mm 715mm 2530mm
Page 9

2-2
2.3 The machine
2.3.1 Description
Radial drills are purposely designed to process bulky objects. Tailift has 20 years
of history and experience in behind. It knows radial drills certainly very well.
Tailift radial drills will be your best choice. T
he material that the machine can
process on are : mild steel, metal, stainless steel, cast iron, aluminum, copper,,,, etc,
except magnesium alloy. (Note 1)
Note 1: Processing magnesium alloy may cause fire.
2.3.2 Parts
Ⅰ
ⅠⅠ
Ⅰ. For TPR-720A, TPR-820A, TPR-920A
There are six categories of parts on the radial drill: Gearbox, Arm, Column,
Top Cover, Box Table and Base. The following are its description and locations.
1. Base The main aim of the base is to support the whole weight of the
machine. In addition, the cutting fluid is contained here and the
Box Table is installed on.
2.
2.2.
2.
Gear box It is the core part for the radial drill for all procession is finished
here, like speed switch, auto feed, spindle,,, etc. They are inside
of the gearbox.
3. Arm It is to support the gearbox and is connected with the column.
4. Column It is to support the gearbox and the arm. It connects the base.
5. Top Cover It is on the top of the machine, where there is a motor. The
motor is to run the gearbox, rise and lower the arm.
6. Box table Working with clamps, it enables to reach the required accuracy.
Page 10

2-3
Ⅱ
ⅡⅡ
Ⅱ. only for TPR-1100
There are six categories of parts on the radial drill: Gearbox, Arm, Column, Top
Cover, Box Table and Base. The following are its description and locations.
1. Base The main aim of the base is to support the whole weight of the
machine. In addition, the cutting fluid is contained here and the
Box Table is installed on.
2.
2.2.
2.
Gear box It is the core part for the radial drill for all procession is finished
here, like speed switch, auto feed, spindle,,, etc. They are inside
of the gearbox.
3. Arm It is to support the gearbox and is connected with the column.
4. Column It is to support the gearbox and the arm. It connects the base.
5. Top Cover It is at the top end of the Column.
6.
6.6.
6.
Box table Working with clamps, it enables to reach the required accuracy.
7. The ball screw
transmit ion
motor
The motor is to elevate the gearbox.
Page 11

2-4
2.4 Specifications.
2.4.1 TPR-720A Specification.
TPR-720A
The Column diameter 210mm
Distance from the column surface to the spindle center,
max
750mm
Distance from the column surface to the spindle center,
min
220mm
Horizontal travel of the Spindle head. 530mm
Distance from the Base surface to the Spindle end, max. 1060mm
Distance from the Base surface to the Spindle end, min. 260mm
Elevating height of the Arm. 580mm
Effective area of the Box Table. 600mm╳╳╳╳445mm╳╳╳╳380mm
The dimensions of the Base (L ╳╳╳╳ W ╳╳╳╳ H) 1250mm╳╳╳╳640mm╳╳╳╳160mm
Taper hole of the Spindle. MT#4
Stroke of the Spindle. 220mm
R.P.M. of the Spindle.((((rounds╱╱╱╱min.╳╳╳╳ step)))) 88,154,282,455,796,1500six steps
Feed rate of the Spindle((((MM╱╱╱╱round╳╳╳╳speed)))) 0.05,0.09,0.15 3 speeds.
Horse Power of the main motor. 1.5KW(2HP)
Horse Power of the elevating motor. 0.75KW(1HP)
Horse Power of the cooling pump motor. 0.1KW(1/8HP)
The machine height from floor, max. 2170mm
Height from the Column top to floor 1850mm
Net weight (approx.) kgs 1120kg
Shipping Gross weight. (approx.) kgs 1250kg
Shipping dimensions(L╳╳╳╳W╳╳╳╳H) 1625mm╳╳╳╳810mm╳╳╳╳2160mm
The max. processing capacity.
Steel ∅∅∅∅32
Drilling
Cast iron ∅∅∅∅50
Steel ∅∅∅∅25
Tapping
Cast Iron ∅∅∅∅32
Page 12

2-5
2.4.2 TPR-820A Specification.
TPR-820A
The Column diameter 210mm
Distance from the column surface to the spindle center, max
850mm
Distance from the column surface to the spindle center, min
220mm
Horizontal travel of the Spindle head. 630mm
Distance from the Base surface to the Spindle end, max. 1210mm
Distance from the Base surface to the Spindle end, min. 350mm
Elevating height of the Arm. 640mm
Effective area of the Box Table. 600mm╳╳╳╳445mm╳╳╳╳380mm
The dimensions of the Base (L ╳╳╳╳ W ╳╳╳╳ H) 1250mm╳╳╳╳640mm╳╳╳╳160mm
Taper hole of the Spindle. MT#4
Stroke of the Spindle. 220mm
R.P.M. of the Spindle.((((rounds╱╱╱╱min.╳╳╳╳ step)))) 88,154,282,455,796,1500 6 steps
Feed rate of the Spindle((((MM╱╱╱╱round╳╳╳╳speed)))) 0.05,0.09,0.15 3 speeds
Horse Power of the main motor. 1.5KW(2HP)
Horse Power of the elevating motor. 0.75KW(1HP)
Horse Power of the cooling pump motor. 0.1KW(1/8HP)
The machine height from floor, max. 2320mm
Height from the Column top to floor 2010mm
Net weight (approx.)kgs 1200 kg
Shipping Gross weight. (approx.)kgs 1340 kg
Shipping dimensions(L╳╳╳╳W╳╳╳╳H) 1680mm╳╳╳╳810mm╳╳╳╳2210mm
The max. processing capacity.
Steel ∅∅∅∅32
Drilling
Cast iron ∅∅∅∅50
Steel ∅∅∅∅25
Tapping
Cast Iron ∅∅∅∅32
Page 13

2-6
2.4.3 TPR-920A specification.
TPR-920A
The Column diameter 210mm
Distance from the Column surface to the Spindle center, max.
950mm
Distance from the Column surface to the Spindle center, min.
220mm
Horizontal travel of the Spindle head. 730mm
Distance from the Base surface to the Spindle end, max. 1210mm
Distance from the Base surface to the Spindle end, min. 350mm
Elevating height of the Arm. 640mm
Effective area of the Box Table. 600mm╳╳╳╳445mm╳╳╳╳380mm
The dimensions of the Base (L ╳╳╳╳ W ╳╳╳╳ H) 1250mm╳╳╳╳640mm╳╳╳╳160mm
Taper hole of the Spindle. MT#4
Stroke of the Spindle. 220mm
R.P.M. of the Spindle.((((rounds╱╱╱╱min.╳╳╳╳ step)))) 88,154,282,455,796,1500 6
steps
Feed rate of the Spindle((((MM╱╱╱╱round╳╳╳╳speed)))) 0.05,0.09,0.15 3 speeds
Horse Power of the main motor. 1.5KW(2HP)
Horse Power of the elevating motor. 0.75KW(1HP)
Horse Power of the cooling pump motor. 0.1KW(1/8HP)
The machine height from floor, max. 2320mm
Height from the Column top to floor 2010mm
Net weight (approx.) kgs 1250 kg
Shipping Gross weight. (approx.) kgs 1400 kg
Shipping dimensions(L╳╳╳╳W╳╳╳╳H) 1810mm╳╳╳╳810mm╳╳╳╳2210mm
The max. processing capacity.
Steel ∅∅∅∅32
Drilling
Cast iron ∅∅∅∅50
Steel ∅∅∅∅25
Tapping
Cast Iron ∅∅∅∅32
Page 14

2-7
2.4.4 TPR-1100 specification.
TPR-1100
The Column diameter 260mm
Distance from the Column surface to the Spindle center, max.
1100mm
Distance from the Column surface to the Spindle center, min.
280mm
Horizontal travel of the Spindle head. 820mm
Distance from the Base surface to the Spindle end, max. 1270mm
Distance from the Base surface to the Spindle end, min. 470mm
Elevating height of the Arm. 570mm
Effective area of the Box Table. 635mm╳╳╳╳520mm╳╳╳╳415mm
The dimensions of the Base (L ╳╳╳╳ W ╳╳╳╳ H) 1710mm╳╳╳╳715mm╳╳╳╳180mm
Taper hole of the Spindle. MT#4
Stroke of the Spindle. 230mm
R.P.M. of the Spindle.((((rounds╱╱╱╱min.╳╳╳╳ step)))) 44-1500 12 steps
Feed rate of the Spindle((((MM╱╱╱╱round╳╳╳╳speed)))) 0.05,0.09,0.153 3 speeds
Horse Power of the main motor. 2.25KW(3HP)
Horse Power of the elevating motor. 0.75KW(1HP)
Horse Power of the cooling pump motor. 0.1KW(1/8HP)
The machine height from floor, max. 2530mm
Height from the Column top to floor 2000mm
Net weight (approx.) kgs 1800 kg
Shipping Gross weight. (approx.) kgs 1950 kg
Shipping dimensions(L╳╳╳╳W╳╳╳╳H) 1880mm╳╳╳╳870mm╳╳╳╳2210mm
The max. processing capacity.
Steel ∅∅∅∅42
Drilling
Cast iron ∅∅∅∅55
Steel ∅∅∅∅25
Tapping
Cast Iron ∅∅∅∅38
Page 15

2-8
2.5 Standard and Option Accessories.
(1) Standard Accessories:
a.
Adjusting tools((((including tool box))))
b.
Cooling equipment((((including pump))))
c.
Lighting installation((((including fluorescent lamp))))
d. Box table
(2) Option Accessories:
a.
Tilt worktable
2.6 Operation position and noise level.
2.6.1
Operation position: about 1 meter far from the gearbox surface.
Height: 1.6 meter from the ground.
2.6.2 The noise level.
(
((
(1)
))
)
Before being processed,
When the turning speed is 1500 rpm, the noise level is 73 dB(A).
When the turning speed is 88 rpm, the noise level is 70 dB(A).
(
((
(2)
))
)
When processing with tools,
The test conditions are as follow:
Material::::SS41
Thickness::::32mm
The tool diameter::::∅∅∅∅32mm
When the turning speed is 88rpm and the feed rate is 0.09 mm, the noise level is 73 dB(A).
When the turning speed is 88rpm and the feed rate is 0.05 mm, the noise level is 71 dB(A).
Page 16

3-1
CHAPTER 3
Preparation to Install
3.1 Space and room requirement
3.1.1 Floor requirement
Using this machine requires solid and well-structured floor and its good level.
Note:
1. For adjusting level, please refer to the chapter 6.
2. Adjusting level i
s needed before using this machine. The level adjusting tolerance
must be within 1 mm/m.
a. For TPR-720A ,TPR-820A ,TPR-920A floor diagrams. (Unit : mm)
The above diagrams are for the bases and ground bolts, as well as its relative positions of
TPR-720A, TPR-820A and TPR-920A.
b. For TPR-1100 floor diagrams (Unit : mm)
The above diagrams are for the bases and ground bolts, as well as its relative positions of
TPR-1100
Page 17

3-2
3.1.2 Space requirement
For safety reason, Path must be considered when installing. For space, it requires:
I
ts calculation is the area of the arm rotating 360 degree, the most outer circle and plus 1000
mm. Different models has different dimensions.
MODEL T
he distance from the column
center to the arm limit.
Plus maintenance area
(A)
Total space
requirement
(B)
TPR-720A
1028 mm 1000 mm 4056 mm
TPR-820A
1128 mm 1000 mm 4256 mm
TPR-920A
1228 mm 1000 mm 4456 mm
TPR-1100
1428 mm 1000 mm 4856 mm
Page 18

3-3
3.2 Environment requirement
a. Never put the machine in the places where sun shines directly on it.
b.
Temperature: normal range is between +5
℃
℃℃
℃ and
40
℃℃℃℃
.
c.
Humidity: between 30% and 95%. At the max. temperature 40
℃℃℃℃,
,,
,The relative
humidity should not be over 50%%%%. And at the relative lower temperature, higher
humidity is acceptable. I.g. at temperature 20℃℃℃℃,humidity 90%%%% is fine.
d. Please keep the machine away from gasoline, chemical substances, dust, acid, sulfides,
magnetic interference and explosive environment.
e. Please keep the machine away from the electrical interference source like welding
machine and EDM.
f. The installation ground must be flat.
g. The illumination of the work area: greater than 500lux.
h.
Good ventilation.
i. Please take care there is no hydraulic splash to prevent from anyone slipping tripping
and falling in danger.
3.3 Power supply requirement
a. Acceptable voltage fluctuation : normally ±±±±10%vlt.
b. Acceptable frequency fluctuation : ±±±±1HZ (50/60HZ)
c. Acceptable momentary power-off duration: less than10m.sec
d. Acceptable voltage impulse
The Peak value : 200% or less than the line voltage of the actual value(rms. value)
Duration: 1.5m.sec or less
e. Acceptable AC voltage of the waveform distortion.
f. Acceptable imbalance of the line voltage: 5% or less
g. Power capacity table
Ⅰ
Ⅰ
Ⅰ
Ⅰ.For TPR-720A, TPR-820A, TPR-920A
Main Motor
1.5Kw
Elevating Motor 0.75Kw
Coolant Pump Motor 0.1Kw
The total power requirement should be 5.935KVA
Ⅱ
ⅡⅡ
Ⅱ.Only for TPR-1100
Main Motor
2.25Kw
Elevating Motor 0.75Kw
Coolant Pump Motor 0.1Kw
The total power requirement should be 7.853KVA
Page 19

3-4
3.4 Electric system calculation
3.4.1 For TPR-720A, TPR-820A, TPR-920A
Motor Part Name Rated Power Capacity Maximum Initiate Power
Main Motor 1.5kw 4.2kw
Elevating Motor 0.75kw 2.1kw
Coolant Pump Motor 0.1kw 0.28kw
Total Rated Power Capacity:
(1.5kw+0.75kw+0.1kw)=2.35kw…………………..(1)
Maximum Total Initiate Power Capacity:
(4.2kw+2.1kw+0.28kw)=6.58kw………………….. (2)
Transformer Rated Output Power Capacity for Control Circuits
Model
Item 100VA
Input
AC400V±±±±10% 1∅∅∅∅
Power Supply
Output
AC240V±±±±10% 1∅∅∅∅
Ambient Temperature 0°C To 55°C
S=KVA
P=KW
Pf ××××n = 0.75 (Correction Factors)
S=
KW
Pf××××n(0.75)
P=
2.35Kw
0.75
=3.133KVA………………….. (1)
P=
6.58Kw
0.75
=8.773KVA………………….. (2)
Power Equipment Capacity=
3.133KVA+8.773KVA
2
=5.935KVA
Page 20

3-5
3.4.2 For TPR-1100
M
otor Part Name Rated Power Capacity Maximum Initiate Power
Main Motor 2.25kw 6.3kw
Elevating Motor 0.75kw 2.1kw
Coolant Pump Motor 0.1kw 0.28kw
Total Rated Power Capacity:
(1.5kw+0.75kw+0.1kw)=3.1kw………………….. (1)
Maximum Total Initiate Power Capacity:
(4.2kw+2.1kw+0.28kw)=8.68kw…………………..(2)
Transformer Rated Output Power Capacity for Control Circuits
Model
Item 100VA
Input
AC400V±±±±10% 1∅∅∅∅
Power Supply
Output
AC240V±±±±10% 1∅∅∅∅
Ambient Temperature 0°C To 55°C
S=KVA
P=KW
Pf ××××n = 0.75 (Correction Factors)
S=
KW
Pf××××n(0.75)
P=
3.1Kw
0.75
=4.133KVA………………………(1)
P=
8.68Kw
0.75
=11.573KVA……………………(2)
Power Equipment Capacity=
4.133KVA+11.573KVA
2
=7.853KVA
Page 21

4-1
CHAPTER 4
Transportation and Installation.
4.1 Disassembly and packaging.
4.1.1 General
Electrical equipment should be designed to stand transportation and storage under the
temperature between -25
℃
℃℃
℃ and+55℃℃℃℃. If this is impossible, proper measurements must be
taken to endure the high temperature. The criteria for this measurement is that it can
withstand the affection of the high temperature of +70℃℃℃℃ within 24 hours. Other
considerations like to prevent damage from vibration or shock must be also given.
4.1.2 Packaging.(For TPR-720A, TPR-820A, TPR-920A, TPR-1100)
When sold and being shipped to customer’s plant, The machine needs to be packaged
and fastened in place.
a. The way to fasten the machine is illustrated as above diagram.
b. 1 is the Arm tightening lever::::Tight it clockwise.
c. 2 is the Column tightening lever::::Tight it clockwise.
d. 3 is the gearbox tightening lever::::Tighten it after being pulled upwards and fastened it to
the speed change lever with wire, to prevent the pull lever from falling during
transportation.
e. 4 is a wooden block:
::
:
Due to its weight, it might lose its accuracy during transportation. It is
to support the weight of the Arm and prevent from collision each other when test
running. (Please don’t move it when unpacking.)
f. The block is added to help the Column support the Gearbox.
g. 5 is a fastening screw.:
::
:
When being packaged, the machine needs to be fastened with screws.
Otherwise, the machine might move during transportation and make the center of the
gravity slant, therefore bring the risk that the machine falls.
h. 6 is the wooden crate base::::It will ease the movement by a forklift.
Precaution:
All levers must be tightened. Please refer to the chapter 1, regarding the transportation.
MODEL LENGTH WIDTH HIGHT
TPR-720A 1625mm 810mm 2160mm
TPR-820A 1680mm 810mm 2210mm
TPR-920A 1810mm 810mm 2210mm
TPR-1100 1880mm 870mm 2210mm
Page 22

4-2
4.2 Transportation.
4.2.1 The diagram of the machine weight and its gravity center.
The weight differ due to the different models. Their data is as blow:
MODEL TPR-720A TPR-820A TPR-920A TPR-1100
Total Weight 1250 kgw 1340 kgw 1400 kgw 1950 kgw
Required Forklift 2 tons 2 tons 2 tons 2.5 tons
Note:
Please make sure that the forklift tonnage is suitable for the machine.
The above arrow pointed
place is the machine’s gravity
center. It is about 200 mm far from the Column, measured
from the middle of the wooden crate.
4.2.2 The movement of the machine.
The follow is using forklift to move the machine.
The following is the procedure, precaution and illustration for moving the machine with
forklift.
a.
Have a suitable forklift move to the wooden crate.
b. As diagram shown, insert two forks into the underneath of the
wooden crate.
c. Adjust the distance from the forks to the gravity center till L1 is
equal to L2. (L1 & L2=350mm)
d. Have forks fully inserted into the underneath of the wooden
crate.
e.
Have the machine fastened to the forks and forklift, using metal
chain or wire.
Precaution::::
a. Forks must be fully inserted.
b. L1 must be equal to L2 so that the machine can be in balance.
Page 23

4-3
4.2.3 The order to pack
Please pack according the following procedure:
1. P
lace the base plate 1 under the machine and have both the plate and the machine
fastened with bolts.
2. Install the side plate 2.
3. Install the side plate 3.
4. Install the side plate 4.
5. Install the side plate 5.
6.
Install the top plate 6 and pack it.
Page 24

4-4
4.3 Installation of the machine.
4.3.1 Have the machine set onto the fastening bolts of the crate base.
(1) Tools
Sling, lifting equipment, spanner, movement plate, insertion blocks and level
adjusting blocks.
(2) Procedure
a. After dismantling the wooden crate, get the manuals and tool box out.
b. Remove the fastening bolts.
c. Hook it using sling, lift it up and move to site for installation.
d.
Align the ground bolts and the base bores and set the later onto them.
Meanwhile, have the level adjusting blocks inserted to the underneath of the level
adjusting bolts.
e. Remove the lifting equipment and slings.
f. Have nuts for the ground bolts mounted.
Page 25

4-5
4.3.2 Level adjusting.
(1) Tools
a. A level scale, with tolerance within 0.02mm/m
b. Spanners, Level adjusting blocks.
(2) Procedure
a. Please adjust the level adjusting bolts to contact the level adjusting blocks.
b. Have the level scale put on the worktable.
c. Locate the peak point using the level scale and make it as a reference level.
d.
Adjust the tolerance of the level adjusting bolts to be within one grad using the level
adjusting scale.
1. The level adjusting bolts.
4.3.3 The installation of the electricity.
a.
Prepare long enough wire. (about 30 meters). The diameters for all the models are as
follows:
b. Connect L1、、、、L2 and L3 to the main power switch.
c. Connect the ground wire to PE base.
Note: The following are the main power switches and its other relating data.
Power supply AC±±±±10%1ΦΦΦΦ 50/60HZ±±±±1HZ
Cross-sectional area of phase
conductors supplying the
equipment` (mm2)
Rated current
(A)
Item
Type
220V 380V 415V 440V
PE 220V 380V 415V 440V
Power
equipment
capacity
(KVA)
TPR-720A
2 2 2 2 2 6.578 3.62 3.62 3.62
5.935
TPR-820A
2 2 2 2 2 6.578 3.62 3.62 3.62
5.935
TPR-920A
2 2 2 2 2 6.578 3.62 3.62 3.62
5.935
TPR-1100 3.5 3.5 3.5 3.5 3.5 16.2 9.87 9.14 8.53
7.853
Page 26

4-6
4.4 The test after installation.
a. Have the main power on.
b. Press the emergent stop button to see whether it stops immediately.
c. Power on again.
d.
Please check whether the motor is running smoothly. If there is any errors, Please
select two of the wires L1, L2 and L3 and change its position.
e.
Check every mechanism to see whether it works normally.
4.5 The procedure for dismantling the machine.
The dismantling procedure is the reverse of the installation one.
Page 27
5-1
CHAPTER 5
Operation
5.1 A brief introduction to the relevant operation hardware.
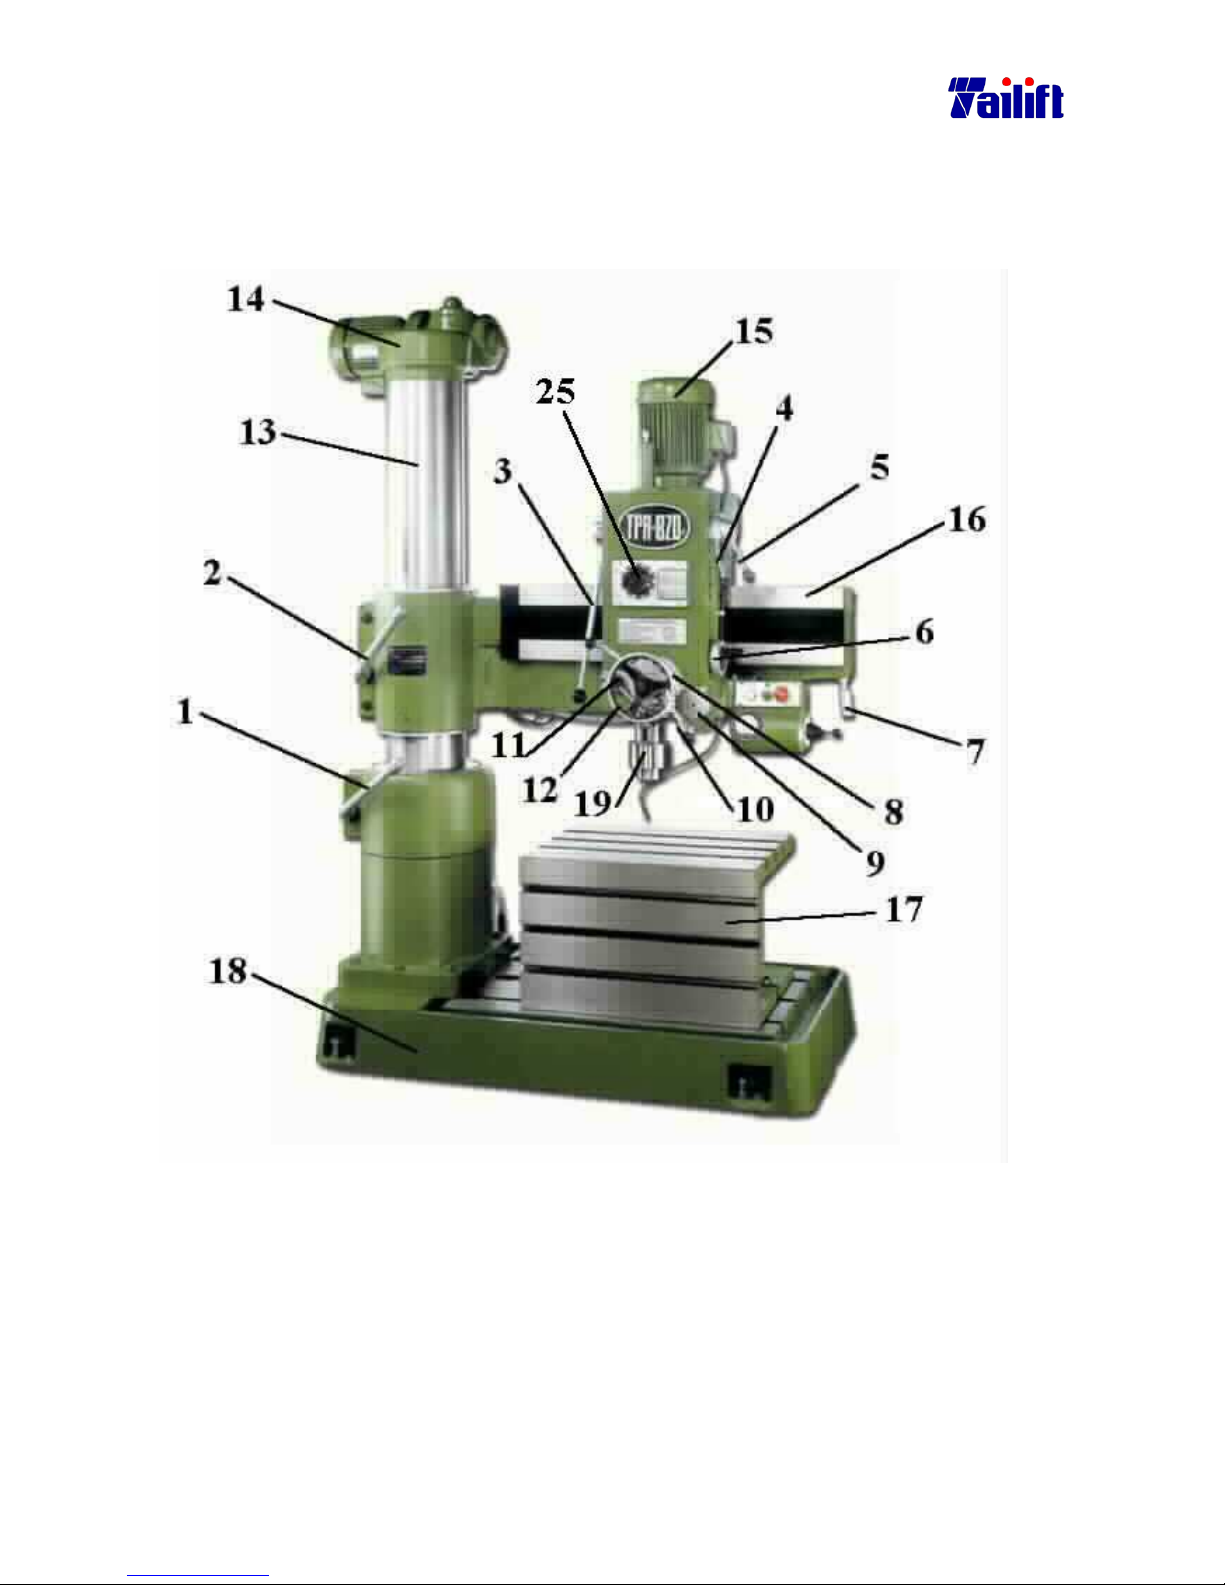
5.1.1
( For TPR-720A, TPR-820A, TPR-920A)
The front view of TPR-820A.
Page 28
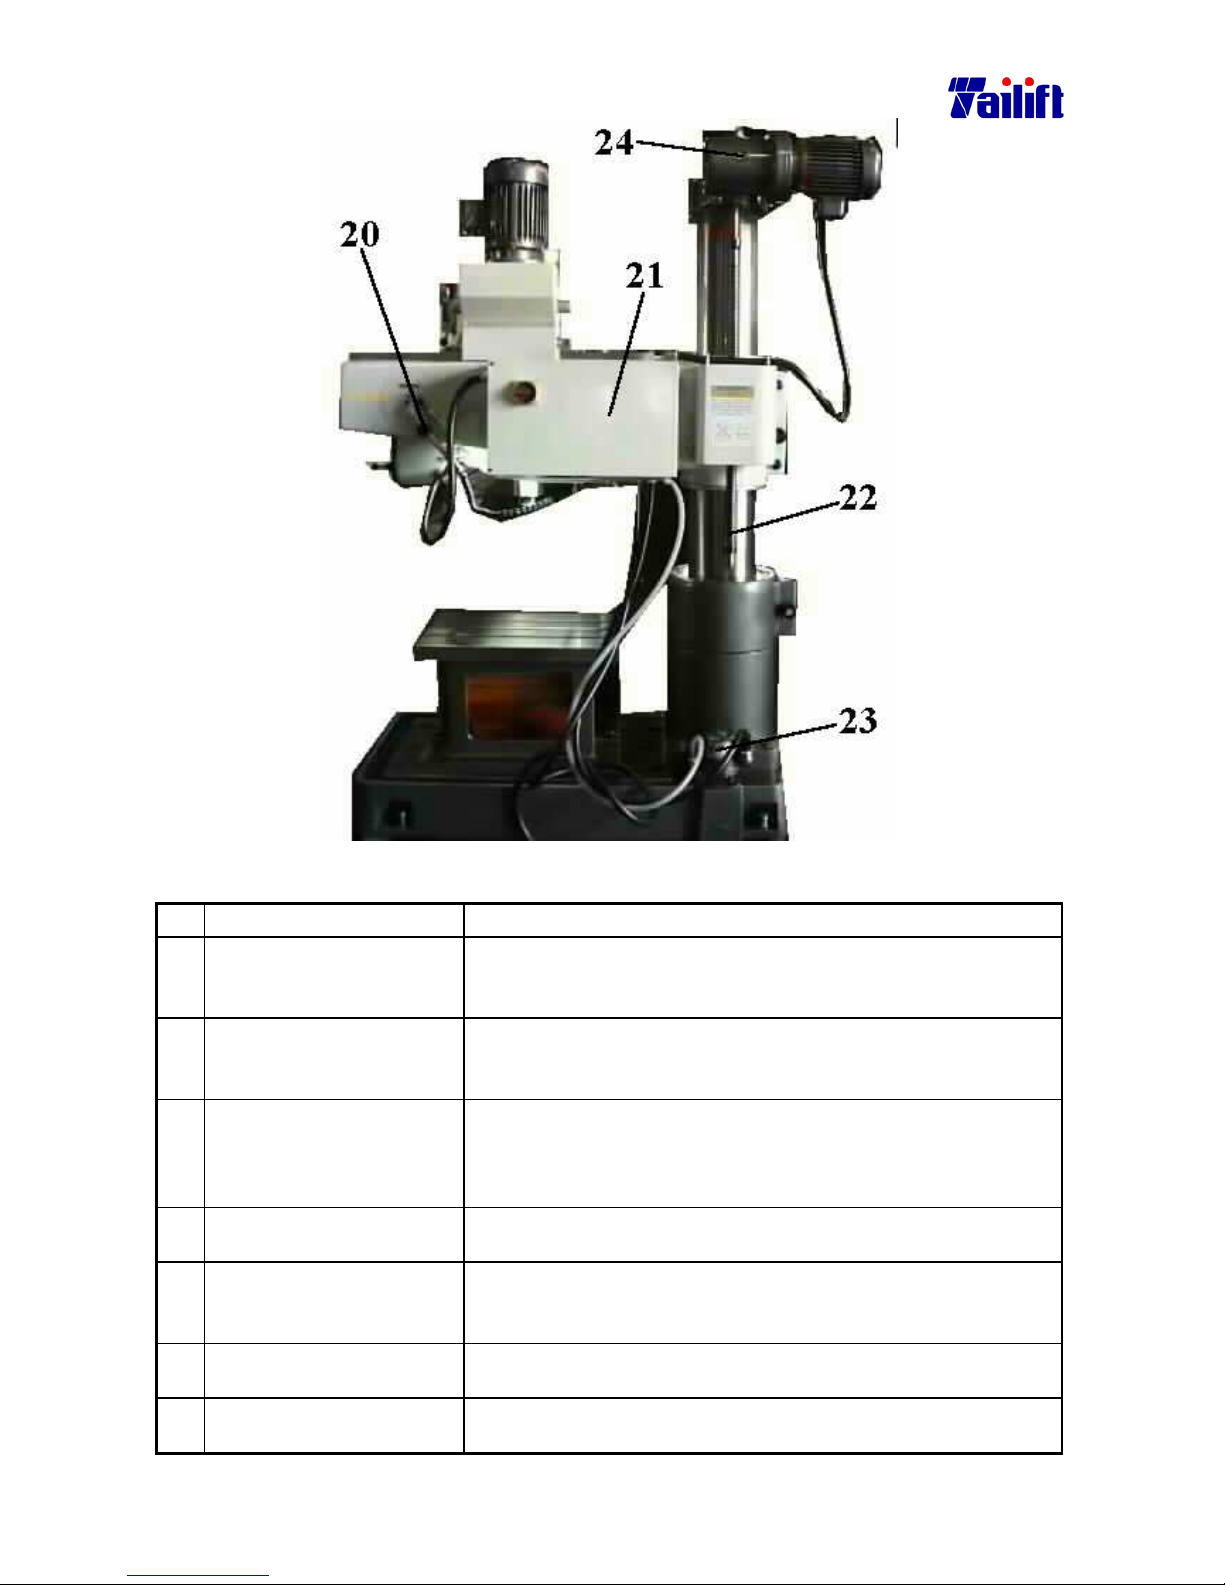
5-2
The rear view of TPR-820A.
The relevant terms. ( For TPR-720A, TPR-820A, TPR-920A)
No.
Term Description
1 Column clamping lever It is to secure the rotation position of the Arm on the
Column. e.g. after arm is rotated to a certain degree, you use
this lever to secure the Arm on the Column.
2 Arm clamping lever It is to secure the lifting or lowering position of the arm. e.g.
after the arm is lifted or lowered to a certain height, you use
this lever to secure the Arm on the Column.
3 Head clamping lever It is to secure the horizontal position of the spindle and
gearbox on the Arm. e.g. after the S
pindle is moved leftwards
or rightwards to a certain position, you use this lever to
secure the Spindle on the Arm.
4 Three speeds change lever It is to change the speed of the Spindle. There are three
speeds for it.
5 Two speeds change lever It is to change between the high and low speed. After
interconnecting with three speeds change lever, there are six
speeds available on the machine.
6 Hand wheel, for moving
head
It is the indicator for the automatic knife feeding. It runs
simultaneously with the feeding knives.
7 Handle, for rotating the
Arm.
It requires the smallest strength and it is the safest way to
rotate the Arm,
Page 29
5-3
8 Main dial It indicated the depth of the drilling. Its scale range is less
than 100 mm.
9 Auxiliary dial It helps you fine dial when the Main Dial is not enough
precision for drilling a certain depth. Its scale range is less
than 220 mm.
10 Lever, for feed trip. It is to start or stop the automatic Knives Feeding.
11 Feed depth lever It is to set up the position of the Main Dial and the Feed Trip.
12 Hand wheel It is to move the head either to right or to left side.
13 Column It is to support the Gearbox and Arm. It is connected with
the Base.
14 Top Cap There is a motor on it, which is to move the Gearbox and
Arm up or downwards.
15 Main motor It is to move the spindle.
16 Arm It is to support the Gearbox, connecting with the Column.
17 Worktable
It features a T shape chamfer, which help clamp and position
work piece. In addition, the worktable helps shorten the
distance between the work piece and the drill bit.
18 Base It is the gravity center of the machine. It stores the cutting
fluids. When no worktable used, it is used to support the
work piece and applied as a base for processing. It features
also a T shape chamfer, which is very convenient for
clamping.
19 Spindle It is the place where drill bit, threading head, drill clamp are
mounted on.
20 Cutting fluids adjusting
knob
It is used to control the floating of the cutting fluids.
21 Control box All control elements are mounted here.
22 Electric ball screw It is the rail of the Arm, which can be lifted or lowered by an
elevating motor.
23 Cutting fluids pump It is to pump the cutting fluids from the container to
lubricate the drilling or boring.
24 Elevating motor It is to elevate up or down the Arm through ball screw.
25 Feed rate switch When at boring and automatic feeding needed, the feed rate
varies due to the different material and drilling bit used. It is
used to adjust the feed rate.
Page 30
5-4
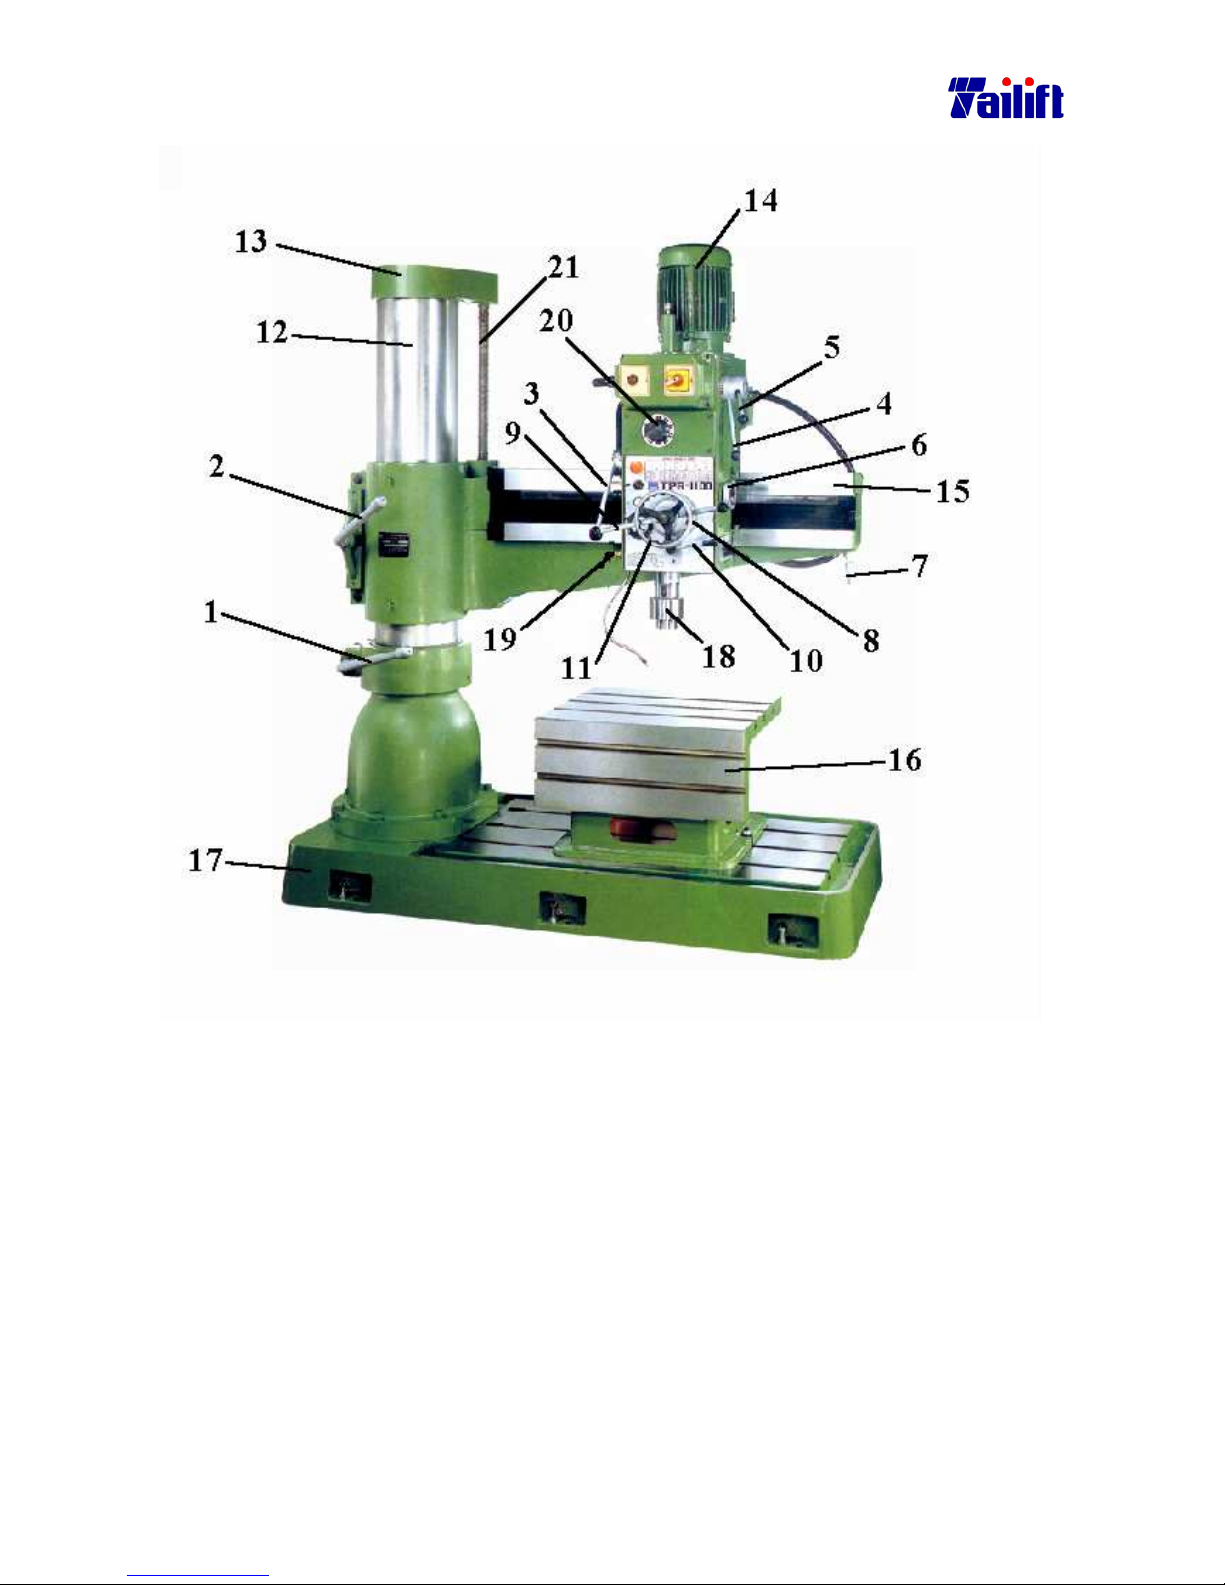
5.1.2 ( For TPR-1100)
The front view of TPR-1100.
Page 31
5-5
The rear view of TPR-1100
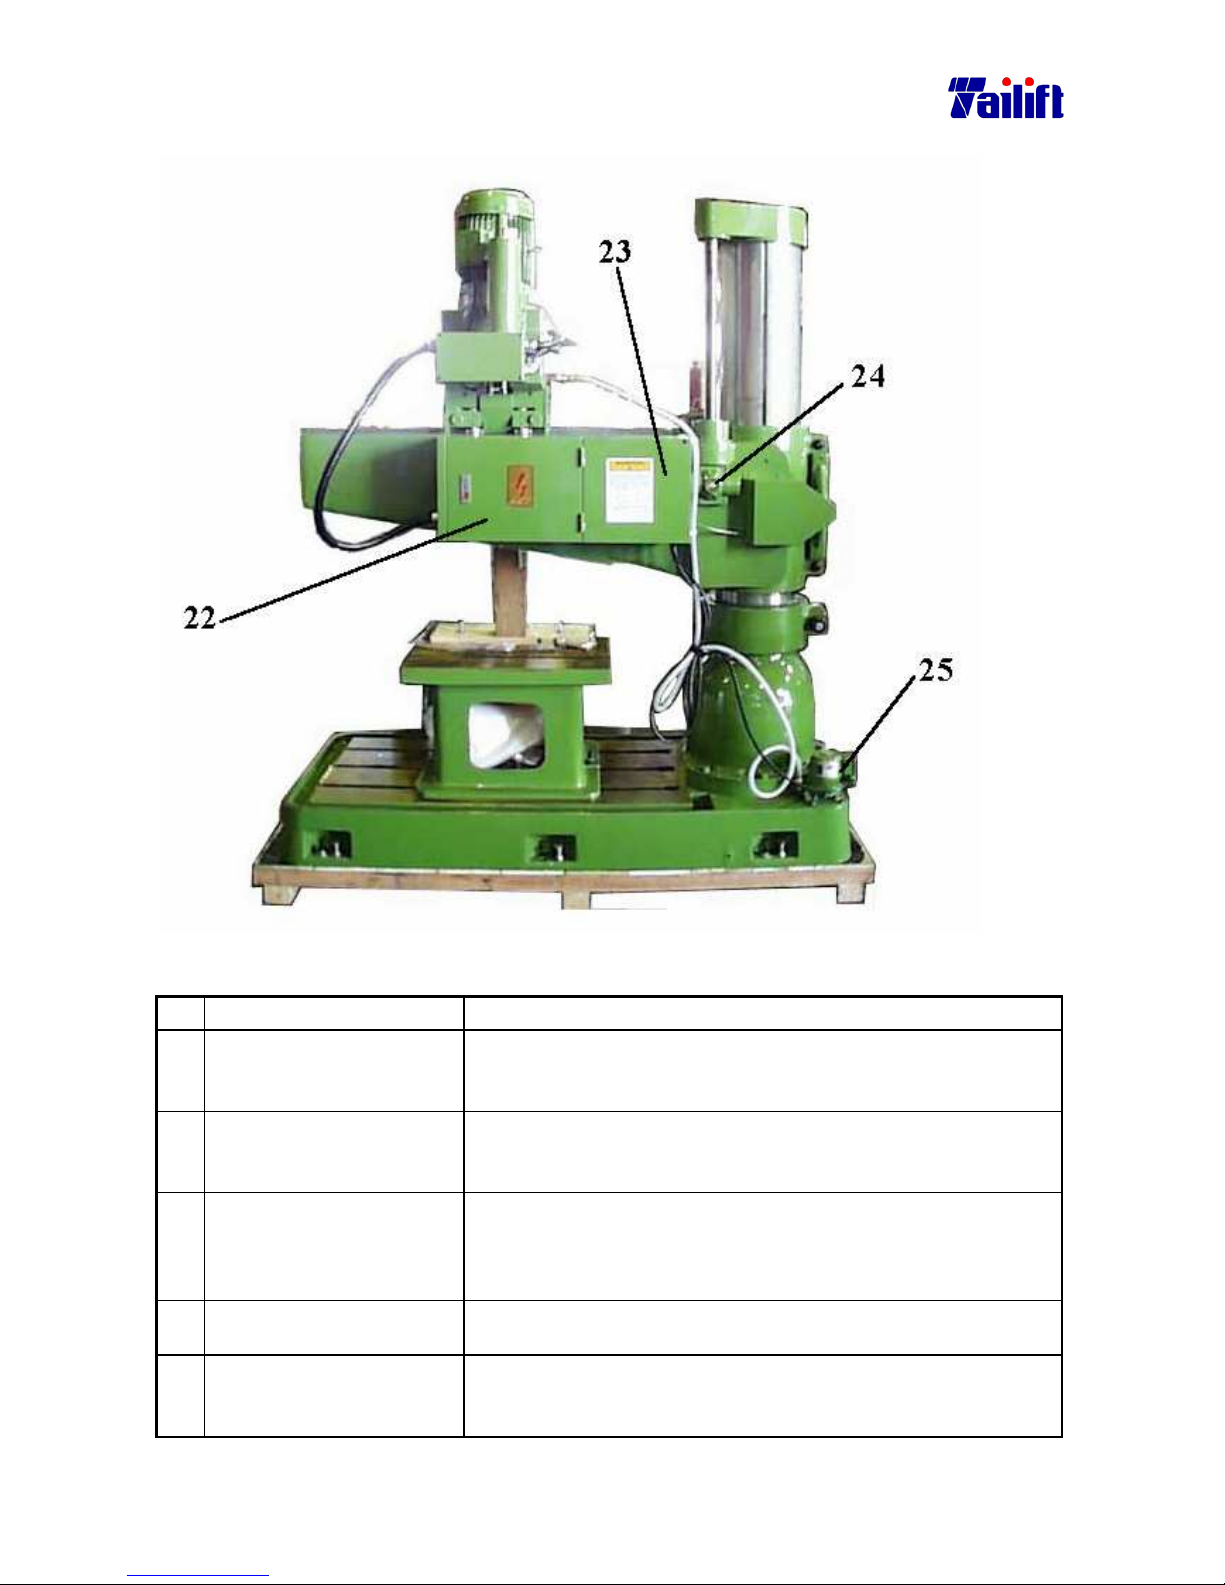
The relevant terms. ( For TPR-1100)
No.
Term Description
1 Column clamping lever It is to secure the rotation position of the Arm on the
Column. e.g. after arm is rotated to a certain degree, you use
this lever to secure the Arm on the Column.
2 Arm clamping lever It is to secure the lifting or lowering position of the arm. e.g.
after the arm is lifted or lowered to a certain height, you use
this lever to secure the Arm on the Column.
3 Head clamping lever It is to secure the horizontal position of the spindle and
gearbox on the Arm. e.g. after the Spindle is moved leftwards
or rightwards to a certain position, you use this lever to
secure the Spindle on the Arm.
4 Three speeds change lever It is to change the speed of the Spindle. There are three
speeds for it.
5 Two speeds change lever It is to change between the high and low speed. After
interconnecting with three speeds change lever, there are six
speeds available on the machine.
Page 32
5-6
6 Hand wheel, for moving
head
It is the indicator for the automatic knife feeding. It runs
simultaneously with the feeding knives.
7 Handle, for rotating the
Arm.
It requires the smallest strength and it is the safest way to
rotate the Arm,
8 Main dial It indicated the depth of the drilling. Its scale range is less
than 100 mm.
9 Lever, for feed trip. It is to start or stop the automatic Knives Feeding.
10 Feed depth lever It is to set up the position of the Main Dial and the Feed Trip.
11 Hand wheel It is to move the head either to right or to left side.
12 Column It is to support the Gearbox and Arm. It is connected with
the Base.
13 Top Cap There is a motor on it, which is to move the Gearbox and
Arm up or downwards.
14 Main motor It is to move the spindle.
15 Arm It is to support the Gearbox, connecting with the Column.
16 Worktable
It features a T shape chamfer, which help clamp and position
work piece. In addition, the worktable helps shorten the
distance between the work piece and the drill bit.
17 Base It is the gravity center of the machine. It stores the cutting
fluids. When no worktable used, it is used to support the
work piece and applied as a base for processing. It features
also a T shape chamfer, which is very convenient for
clamping.
18 Spindle It is the place where drill bit, threading head, drill clamp are
mounted on.
19 Cutting fluids adjusting
knob
It is used to control the floating of the cutting fluids.
20 Feed rate switch When at boring and automatic feeding needed, the feed rate
varies due to the different material and drilling bit used. It is
used to adjust the feed rate.
21 Electric ball screw It is the rail of the Arm, which can be lifted or lowered by an
elevating motor.
22 Control box All control elements are mounted here.
23 Elevating speed reducer The elevating motor rotates very fast. If the motor drives the
ball screw transmission directly, it is very hard to control the
elevating position. Therefore an elevating speed reducer is
mounted to easily control the elevating positions.
24 Metal covering It covers the internal Elevating motor and ball screw so that
the operator or others can be safely protected.
25 Cutting fluids pump It is to pump the cutting fluids from the container to
lubricate the drilling or boring.
Page 33
5-7
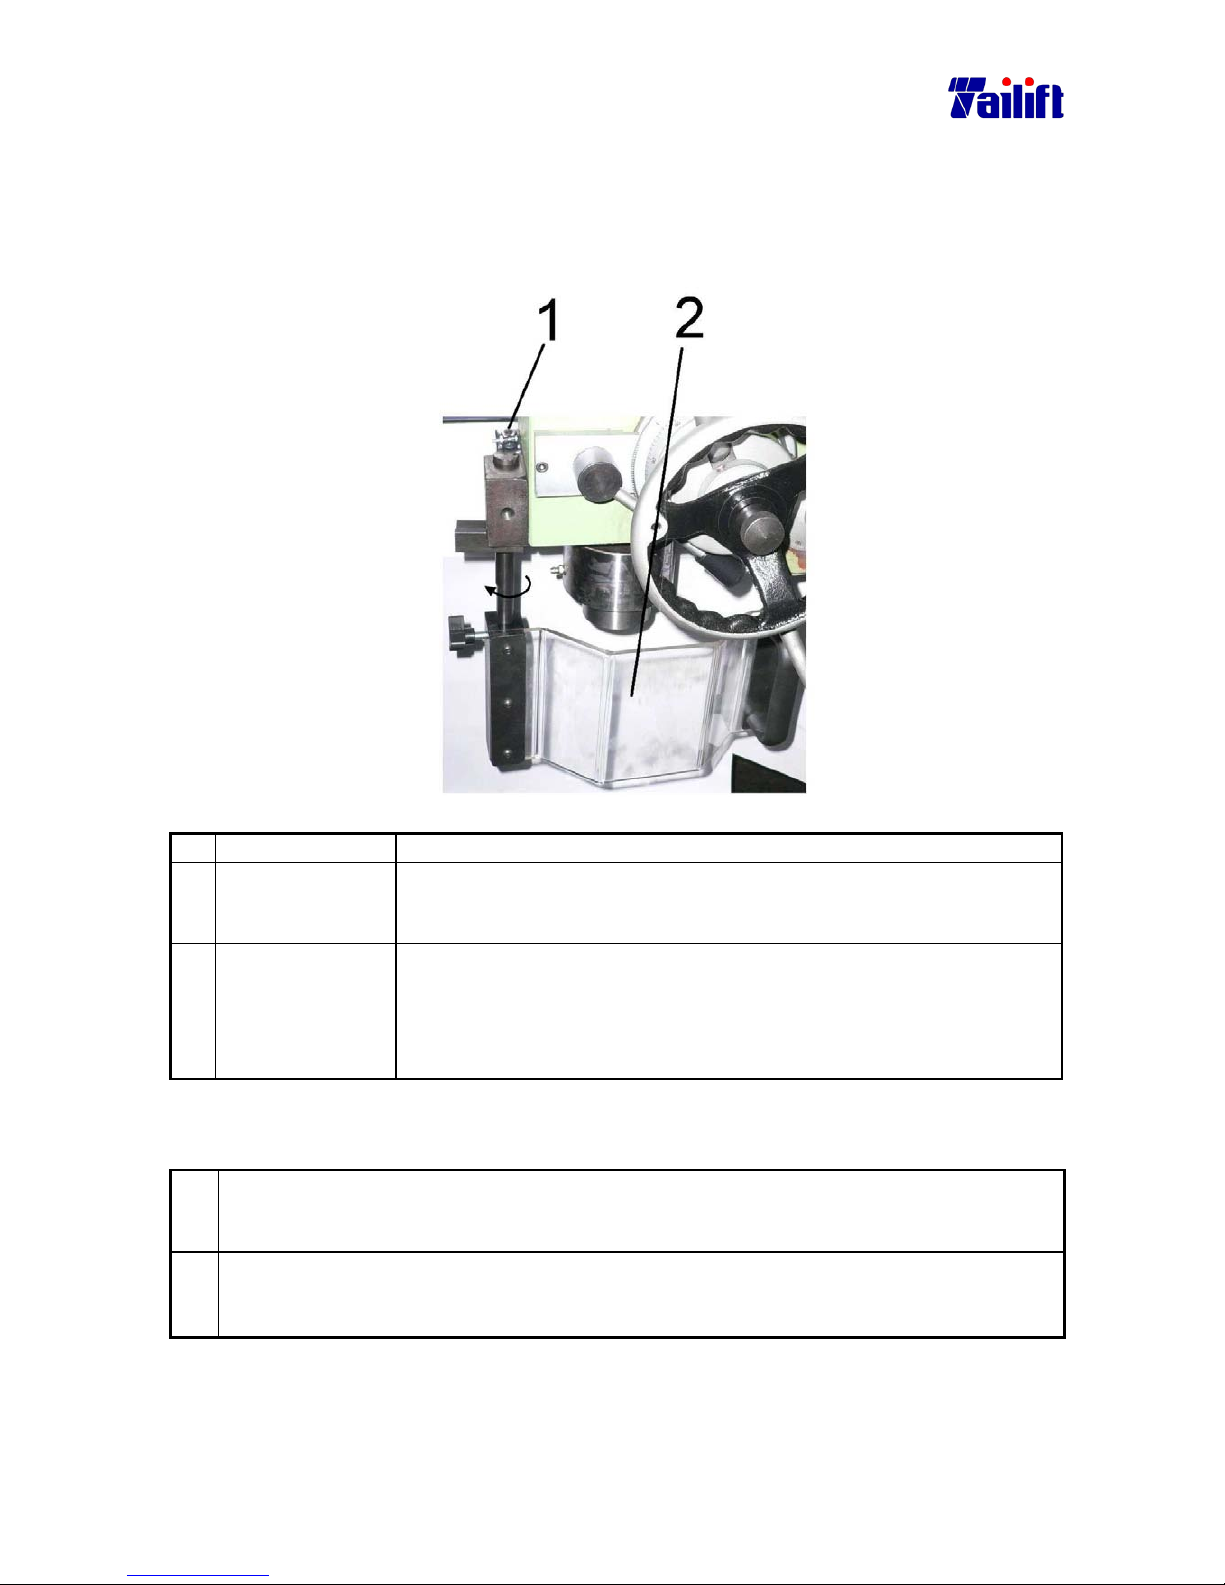
5.1.3 Safty protective device (suit every model)
No.
Term Description
1 Safety Protective
Cover
For to avoid debris fly off. When spindle making the drilling bit,the
cover must be close. Another for safety, the spindle must stop
rotation, when the cover is open.
2 Limit Switch The limit switch is controlled by safety protective cover’s open or
close.
If safety protective cover is open,the spindle stop rotation by limit
switch’ single . Another,if safety protective cover is close,the spindle
can rotation.
Precaution
PrecautionPrecaution
Precaution:
1. When user close the saftety protective cover(As marked 1) , the limit switch (As
marked 2)can message a signal to allow the spindle rotation.Therefore, user can
operation the machine.
2. When user open the saftety protective cover(As marked 1) , the limit switch (As
marked 2)can message a signal to stop the spindle rotation immediately.
Page 34
5-8
5.2 Instruction to switches.
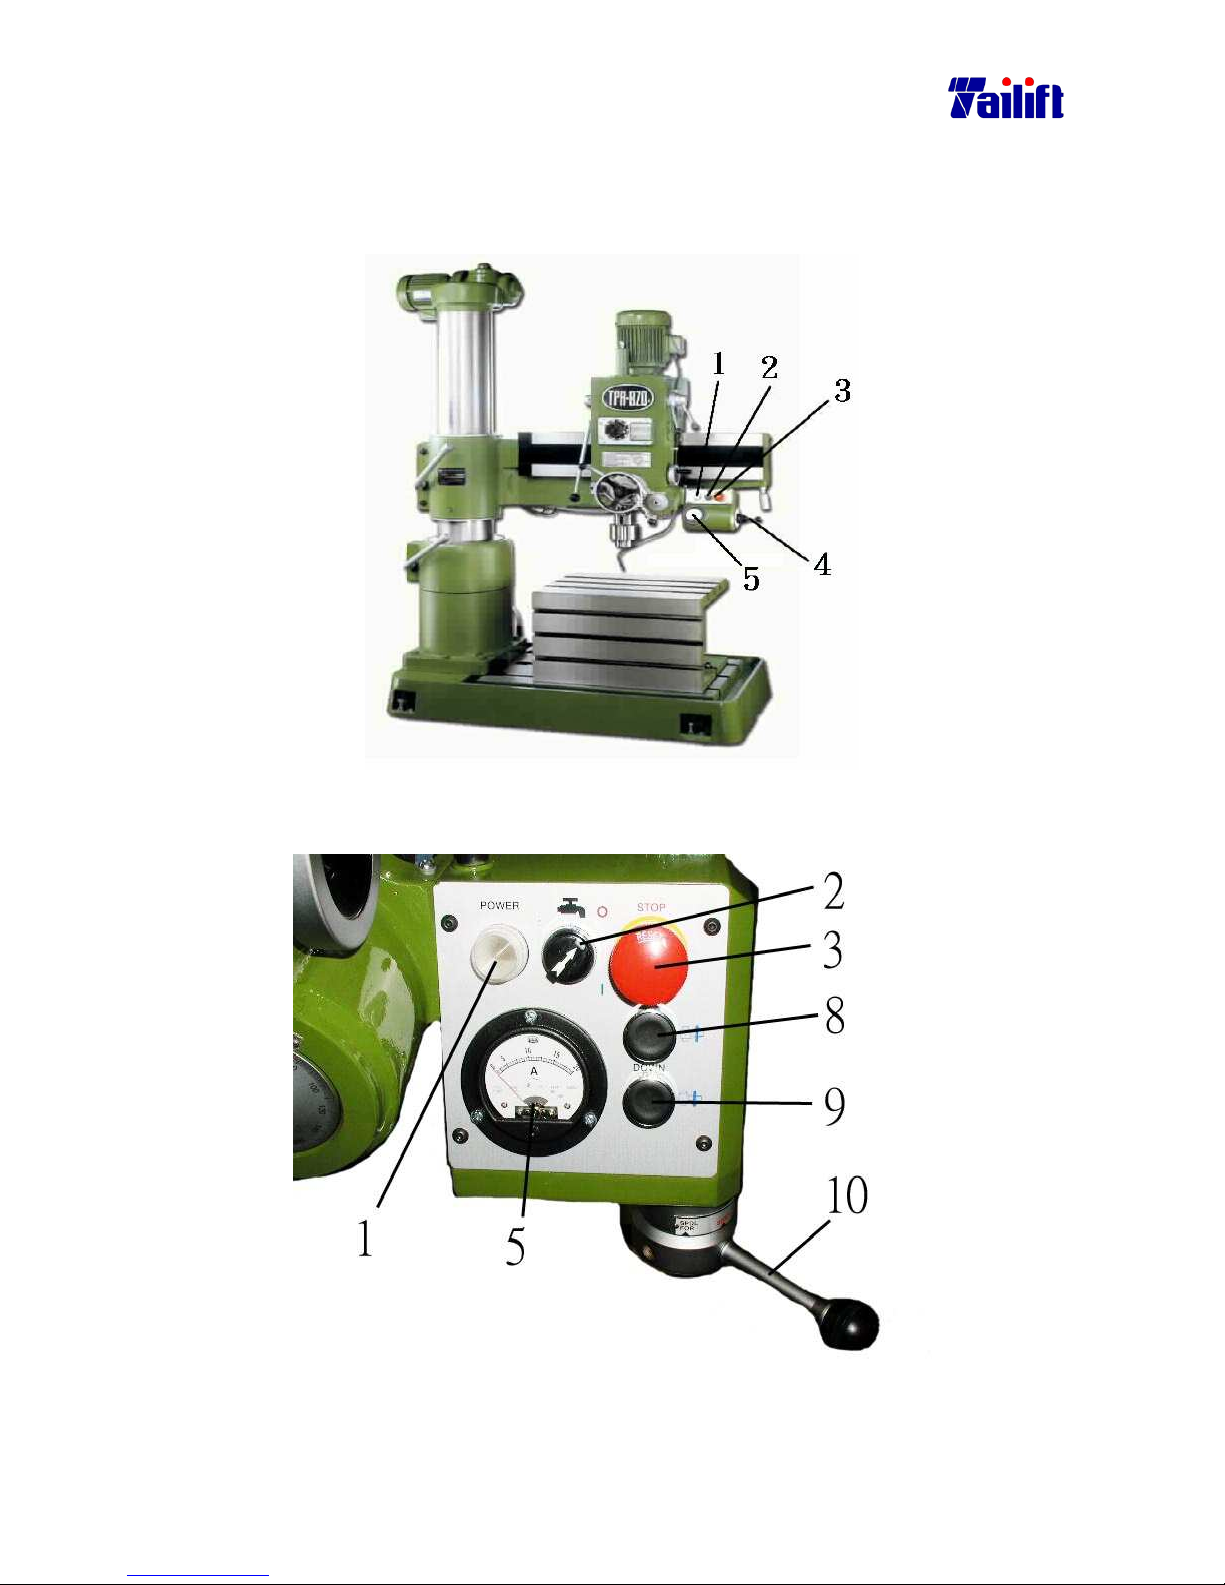
Ⅰ
ⅠⅠ
Ⅰ.( For TPR-720A, TPR-820A, TPR-920A)(Type I)
The front view of TPR-820A
Description for Switches.
( For TPR-720A, TPR-820A, TPR-920A)(Type II)
The rear view of TPR-820A
Page 35
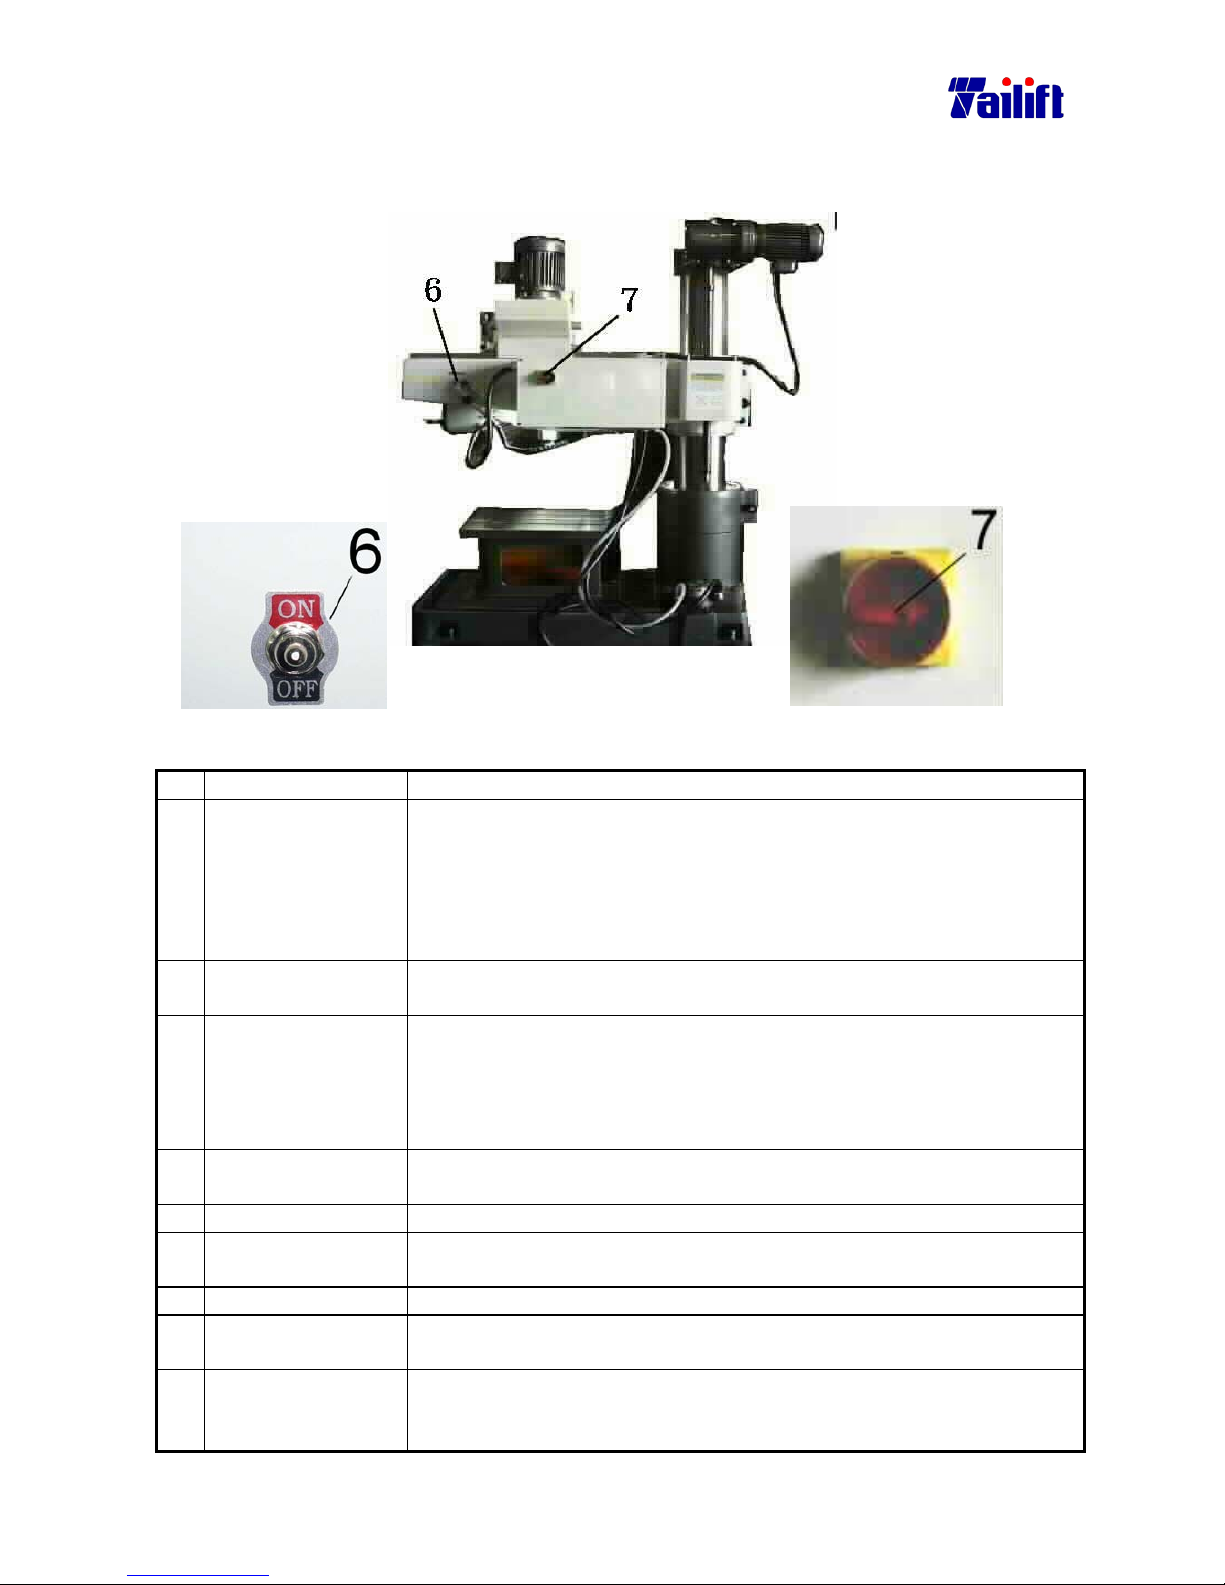
5-9
The rear view of TPR-820A
1. Power-on light It lights when it powers on.
2. The cutting fluids
switch
It is a switch to start on or off the lubrication when at boring, where
the boring or shearing causes high temperature, making the drilling
bit easy to wear. The lubrication can reduce the temperature and
lengthen the life of the drilling bit. Turn on to start and off to stop the
lubrication. The floating capacity is decided by another knob called
the cutting fluids adjusting knob.
3. Emergent stop It is pressed to stop the machine when at processing and emergence
occurs. Pull it again for back to release the stop.
4. Cross switch It is to control the elevating and revolution. There are four sign on it.
When switched to “SPDL. FOR.”, the spindle revolves clockwise.
When switched to “SPDL.REV.
”, it revolves counter clockwise. When
switched to “ARM UP”, the Arm lifts. When switched to “ARM
DOWN”, the arm descends.
5. Electric current
meter
It is for operator’s understanding whether the working situation is
normal.
6. Work light switch It is used to improve lighting where illumination is not enough.
7. Main power switch
It is the terminator of the power connection between the machine and
the power source.
8. Arm uplift switch The arm will uplift when pushing the “up”button.
9. Arm downlift
switch
The arm will be lowered down when pushing the “down” button.
10. Main spindle
forward
-reverse switch
When switch to SPDL.FOR, The spindle will forward . When switch
To SPDL.REV.the spindle will reverse.
Page 36
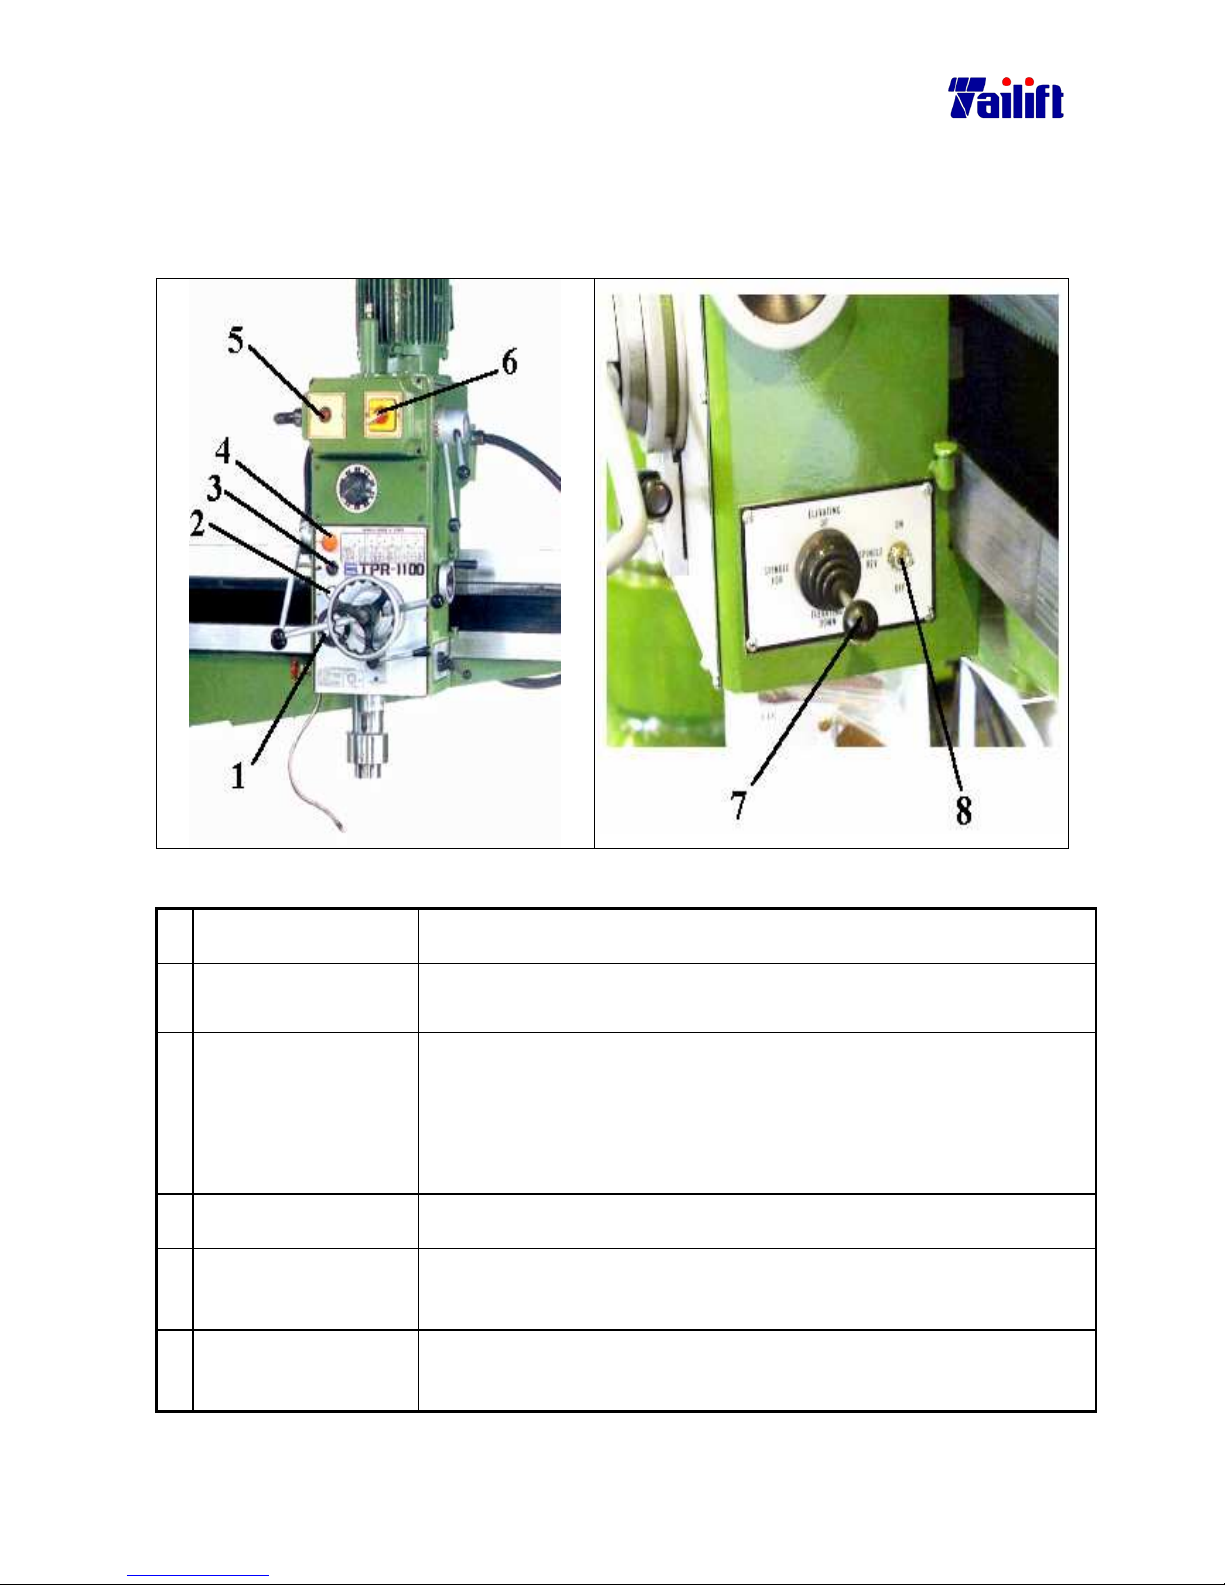
5-10
Ⅱ
ⅡⅡ
Ⅱ.FOR TPR1100(Type I)
Description for Switches.
For TPR-1100 (Type I)
1. Electric current meter It is for operator’s understanding whether the working situation is
normal.
2. Feeding light
It lights when at feeding. After work finished and power off, it turns
off .
3. The cutting fluids
switch
It is a switch to start on or off the lubrication when at boring, where
the boring or shearing causes high temperature, making the drilling
bit easy to wear. The lubrication can reduce the temperature and
lengthen the life of the drilling bit. Turn on to start and off to stop the
lubrication. The floating capacity is decided by another knob called
the cutting fluids adjusting knob.
4. Emergent stop It is pressed to stop the machine when at processing and emergence
occurs. Pull it again for back to release the stop.
5. Power light When the external power and the main machine power switch are on,
The power light will be on ,indicating to the operator that the power
is on.
6 Pole change switch The spindle motor is a pole variable one, a regular motor has 4 pole.
But this one is changeable between 4 and 8 pole . It can change the
Spindle rotating speed.
Page 37
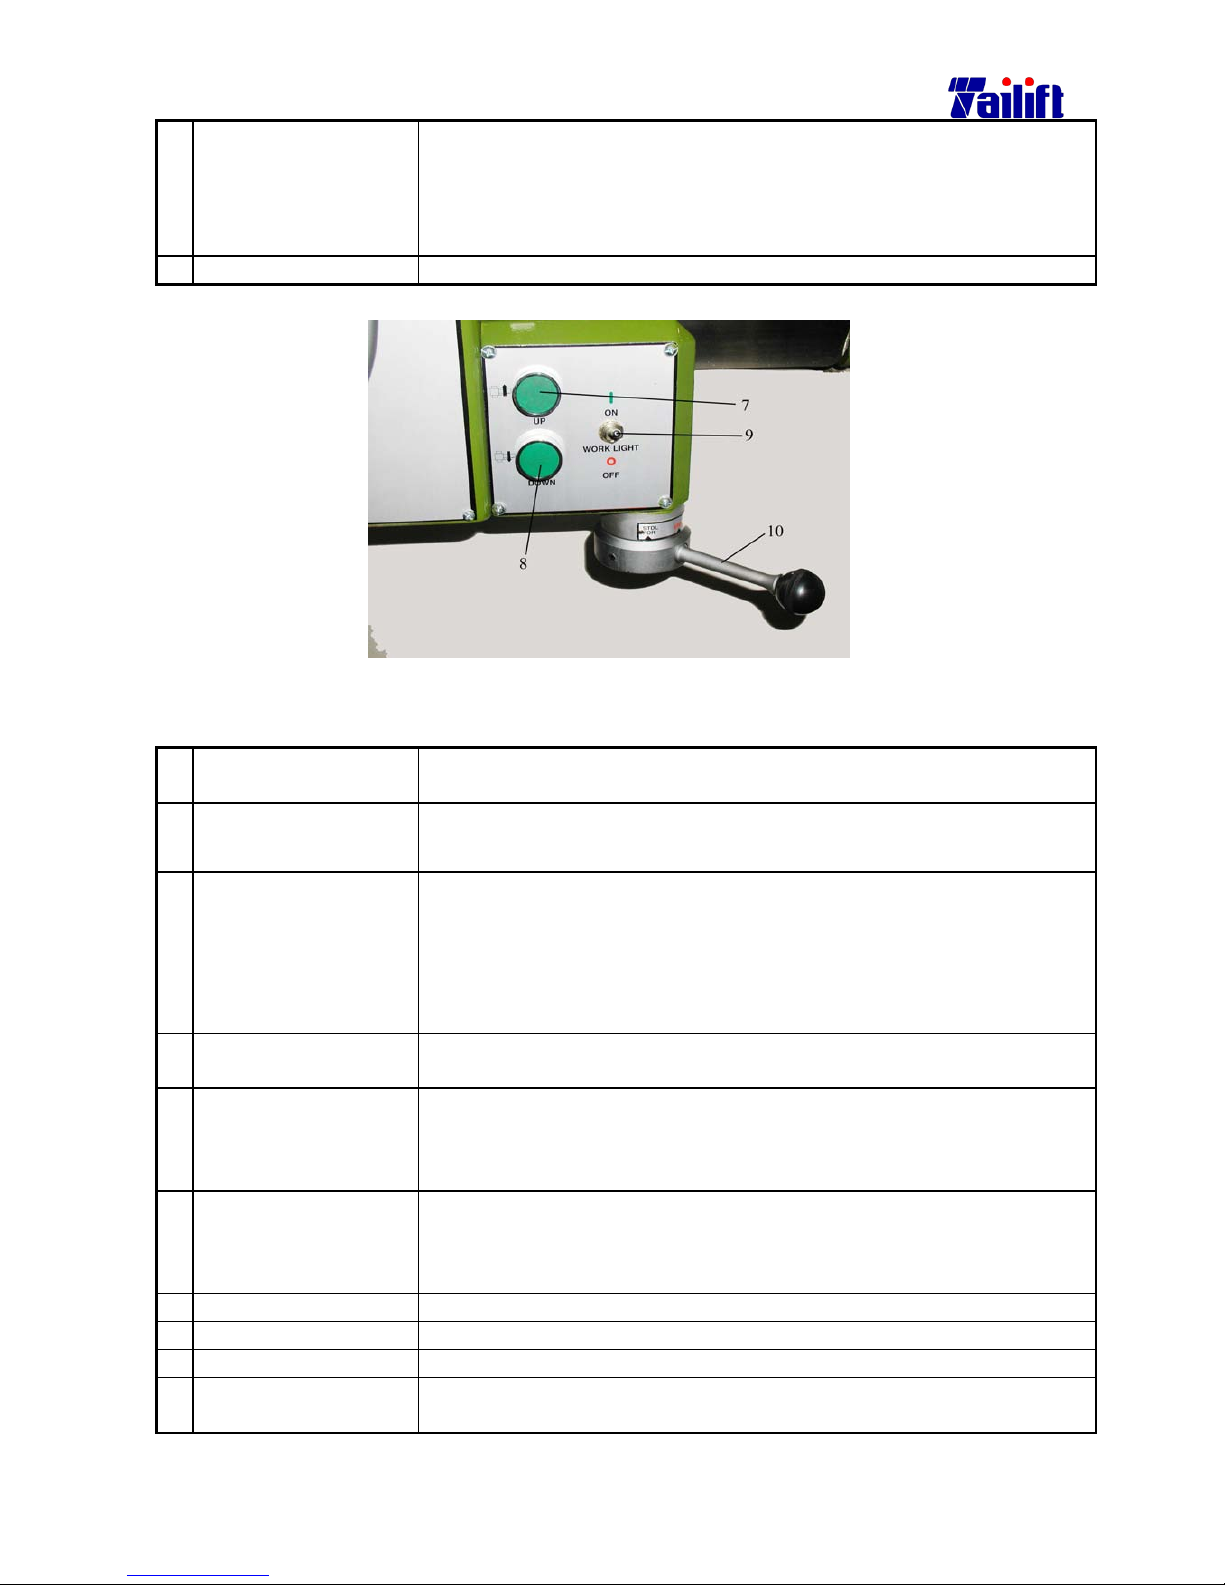
5-11
7. Cross Switch It is to control the elevating and revolution . there are four sign on it.
When switched to “SPDL.FOR.”,the spindle revolves clockwise,
When switched to “SPDL.REV.”,it revolves counter clockwise,
When switched to “Arm UP”, the Arm lifts, When switched to
“Arm Down” , the arm descends.
8. Work light switch It is used to improve lighting where illumination is not enough.
Ⅱ
ⅡⅡ
Ⅱ.For TPR-1100 (Type II)
Description for Switches.
For TPR-1100 (Type II)
1. Electric current meter It is for operator’s understanding whether the working situation is
normal.
2.
Feeding light
It lights when at feeding. After work finished and power off, it turns
off .
3. The cutting fluids
switch
It is a switch to start on or off the lubrication when at boring, where
the boring or shearing causes high temperature, making the drilling
bit easy to wear. The lubrication can reduce the temperature and
l
engthen the life of the drilling bit. Turn on to start and off to stop the
lubrication. The floating capacity is decided by another knob called
the cutting fluids adjusting knob.
4. Emergent stop It is pressed to stop the machine when at processing and emergence
occurs. Pull it again for back to release the stop.
5.
Power light
When the external power and the main machine power switch are on,
the power light will be on, indicating to the operator that the power is
on.
6. Pole change switch
The spindle motor is a pole variable one. A regular motor has 4 pole.
But this one is changeable between 4 and 8 pole. It can change the
spindle rotating speed.
7. Arm uplift switch The arm will uplift when pushing the “up”button.
8. Arm downlift switch The arm will be lowered down when pushing the “down” button.
9. Working lamp switch To lighten the working area.
10. Main spindle forward
-reverse switch
When switch to SPDL.FOR, The spindle will forward . When switch
To SPDL.REV.the spindle will reverse.
Page 38
5-12
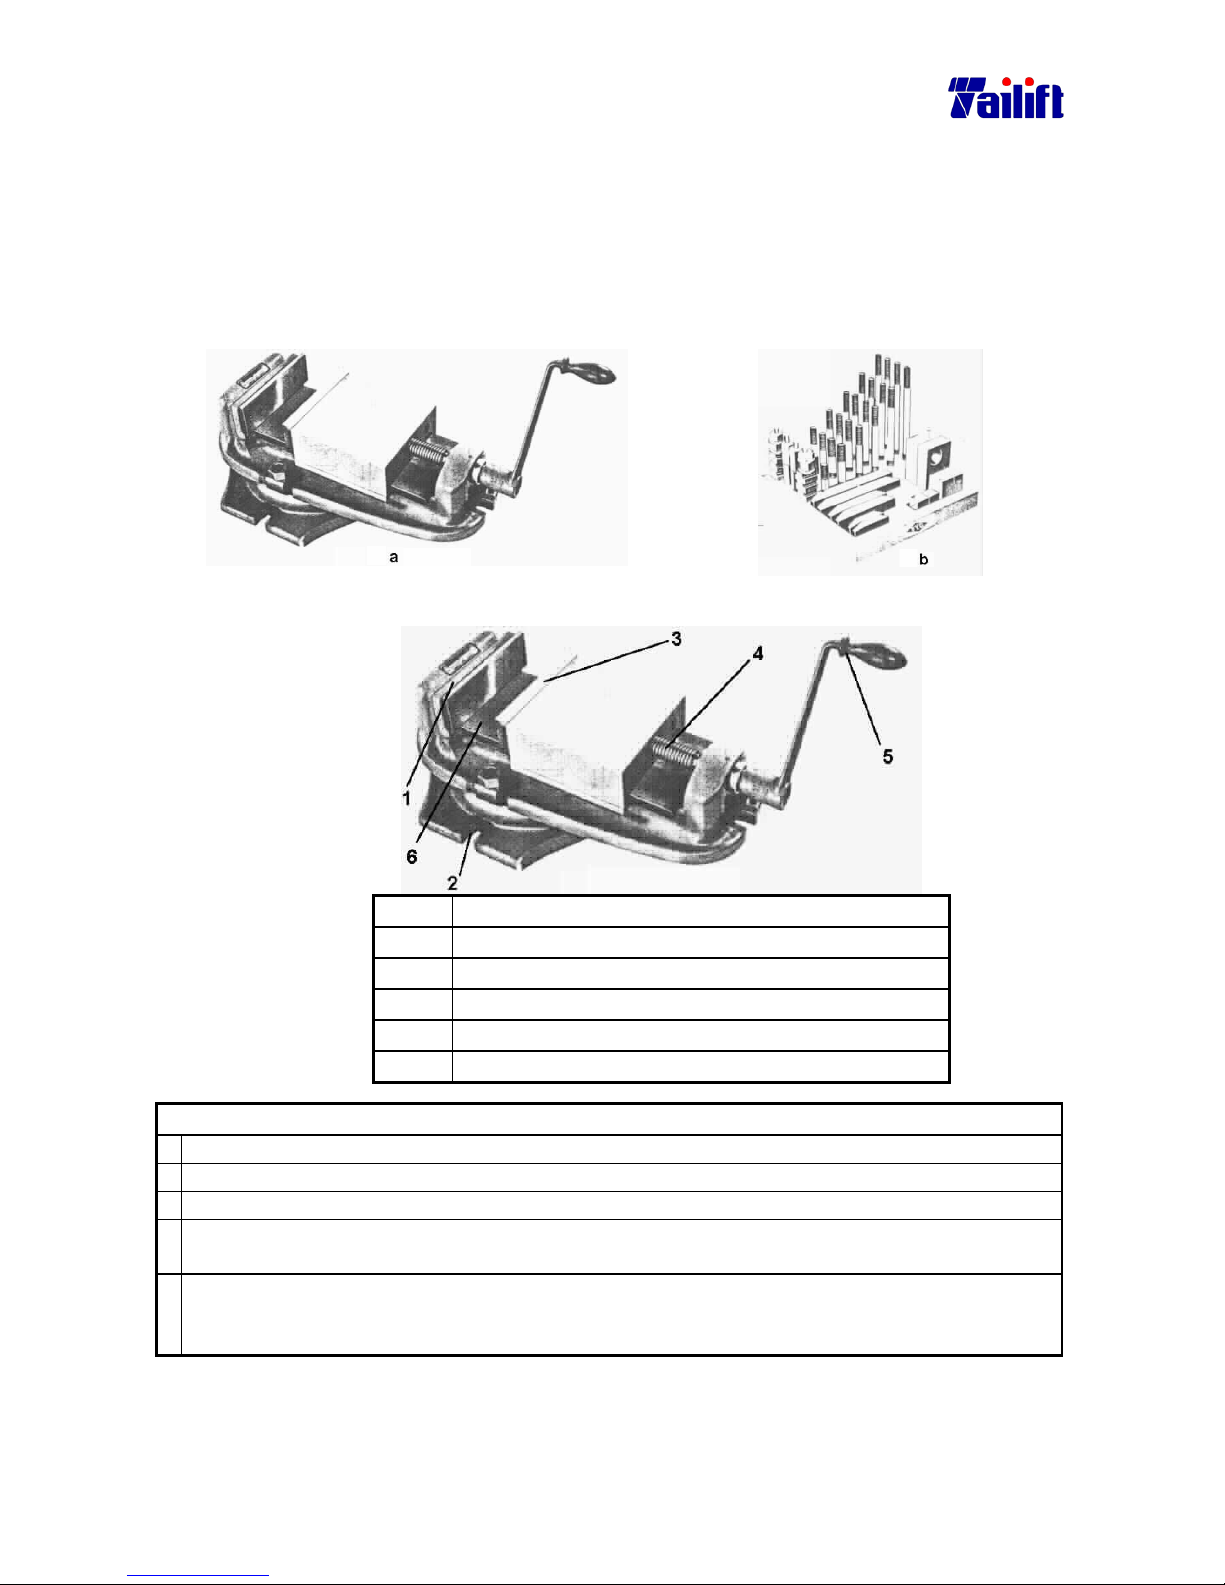
5.3 Installation of the clamp((((work piece))))
5.3.1 General
Work piece must be placed securely and precisely on the radial drill so that
precision and safe procession can be achieved. Regularly, a vise is applied. (as shown
picture a). Since the vise has its range limit, universal clamp (as shown picture b) is
applied for bulky work piece or any work piece which isn’t easy to be clamped. The
universal clamp includes T shape chamfer bolts, stacking plate, insertion blocks, which
makes clamping easier.
5.3.2 Introduction of the vise and the clamping of the work piece.
(
((
(1)))) The fixed side of the vise.
(
((
(2)))) The fixing side with T shape chamfer bolt and nuts
(
((
(3)))) The moving side of the vise.
(
((
(4)))) The screw bar.
(
((
(5)))) The handle.
(
((
(6)))) The surface of the vise.
Clamp work piece as the following::::
a. Move away the drilling bit or lift the gearbox to the utmost point.
b. Using brush, clean the worktable and the vise surface.
c. Clean the vise surface using clean rag.
d. Position the work piece on the vise surface. If it is piercing drilling, please insert a block
under the work piece so that drilling into vise can be avoided.
e. Fasten the handle by rotating it clockwise and tighten it. While tightening it, please use
plastic hammer or copper bar to hit the work piece till there is no gap between the work
piece and the inserted block.
Page 39
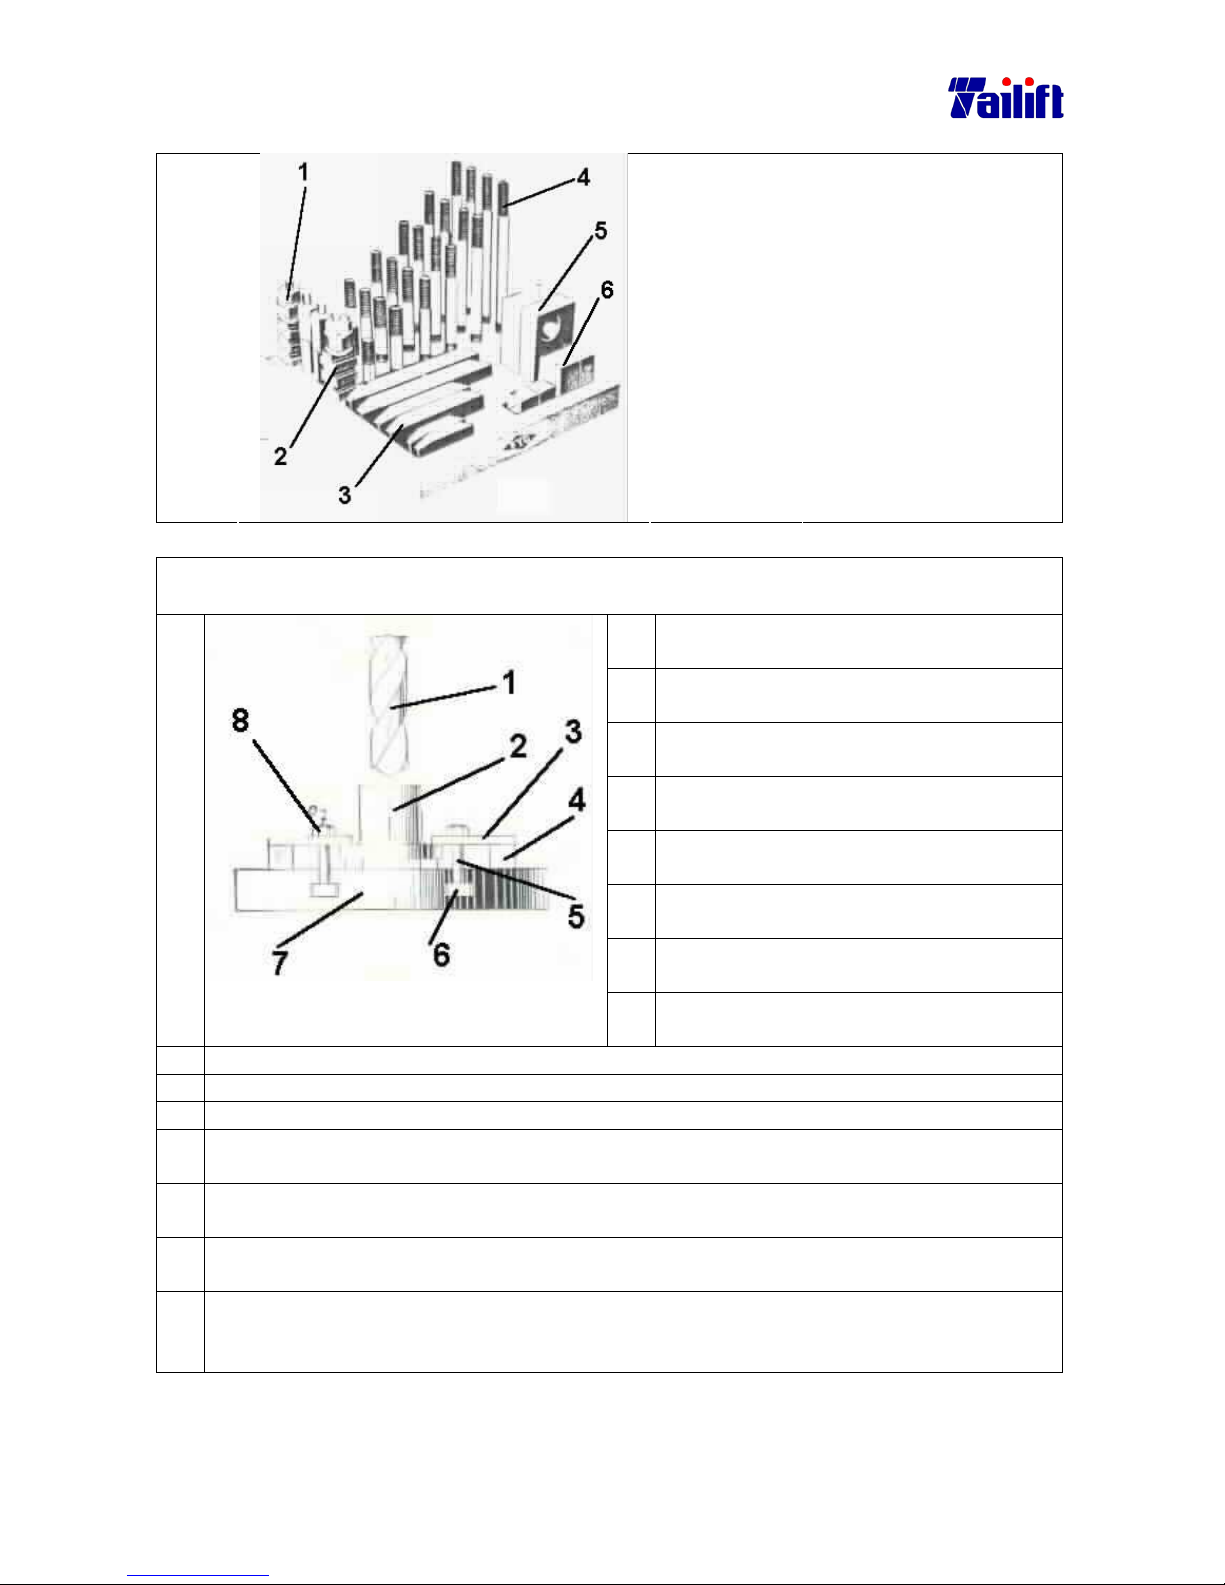
5-13
5.3.3 Universal clamp and the clamping of the work piece.
(
((
(1)
))
)
Hex nuts
(
((
(2)
))
)
T shape chamfer nuts
(
((
(3)
))
)
Stacking plate
(
((
(4)
))
)
Twin head bolts
(
((
(5)
))
)
Insertion block
(
((
(6)
))
)
Ladder block
Clamp the work piece as the following:(
:(:(
:(Since t
he combination of the universal clamp is very
flexible and abundant, The following diagram is applied as an exemplary description.
1. Drilling bit
2. Work piece
3. Stacking block
4. Insertion block
5. Twin head bolts
6. T shape chamfer bolts
7. Worktable
8. Hex but
a. Move away the drilling bit or lift the gearbox to the utmost point.
b. Using brush, clean the worktable and the vise surface.
c. Clean the vise surface using clean rag.
d. Position the work piece on the vise surface. If it is piercing drilling, please insert a block
under the work piece so that drilling into vise can be avoided.
e. After screwing the T shape chamfer nut to the twin head bolts with suitable length, put
it into the T shape chamfer of the worktable or the base.
f. Choose the insertion block or ladder block that is the same high as work flange. Put
them in the other side of the bolts.
g. Using holed stacking block, place them onto the bolts, with one of its side pressing the
work flange and another pressing the insertion block or ladder block, then tighten it
with hex nuts.
Page 40
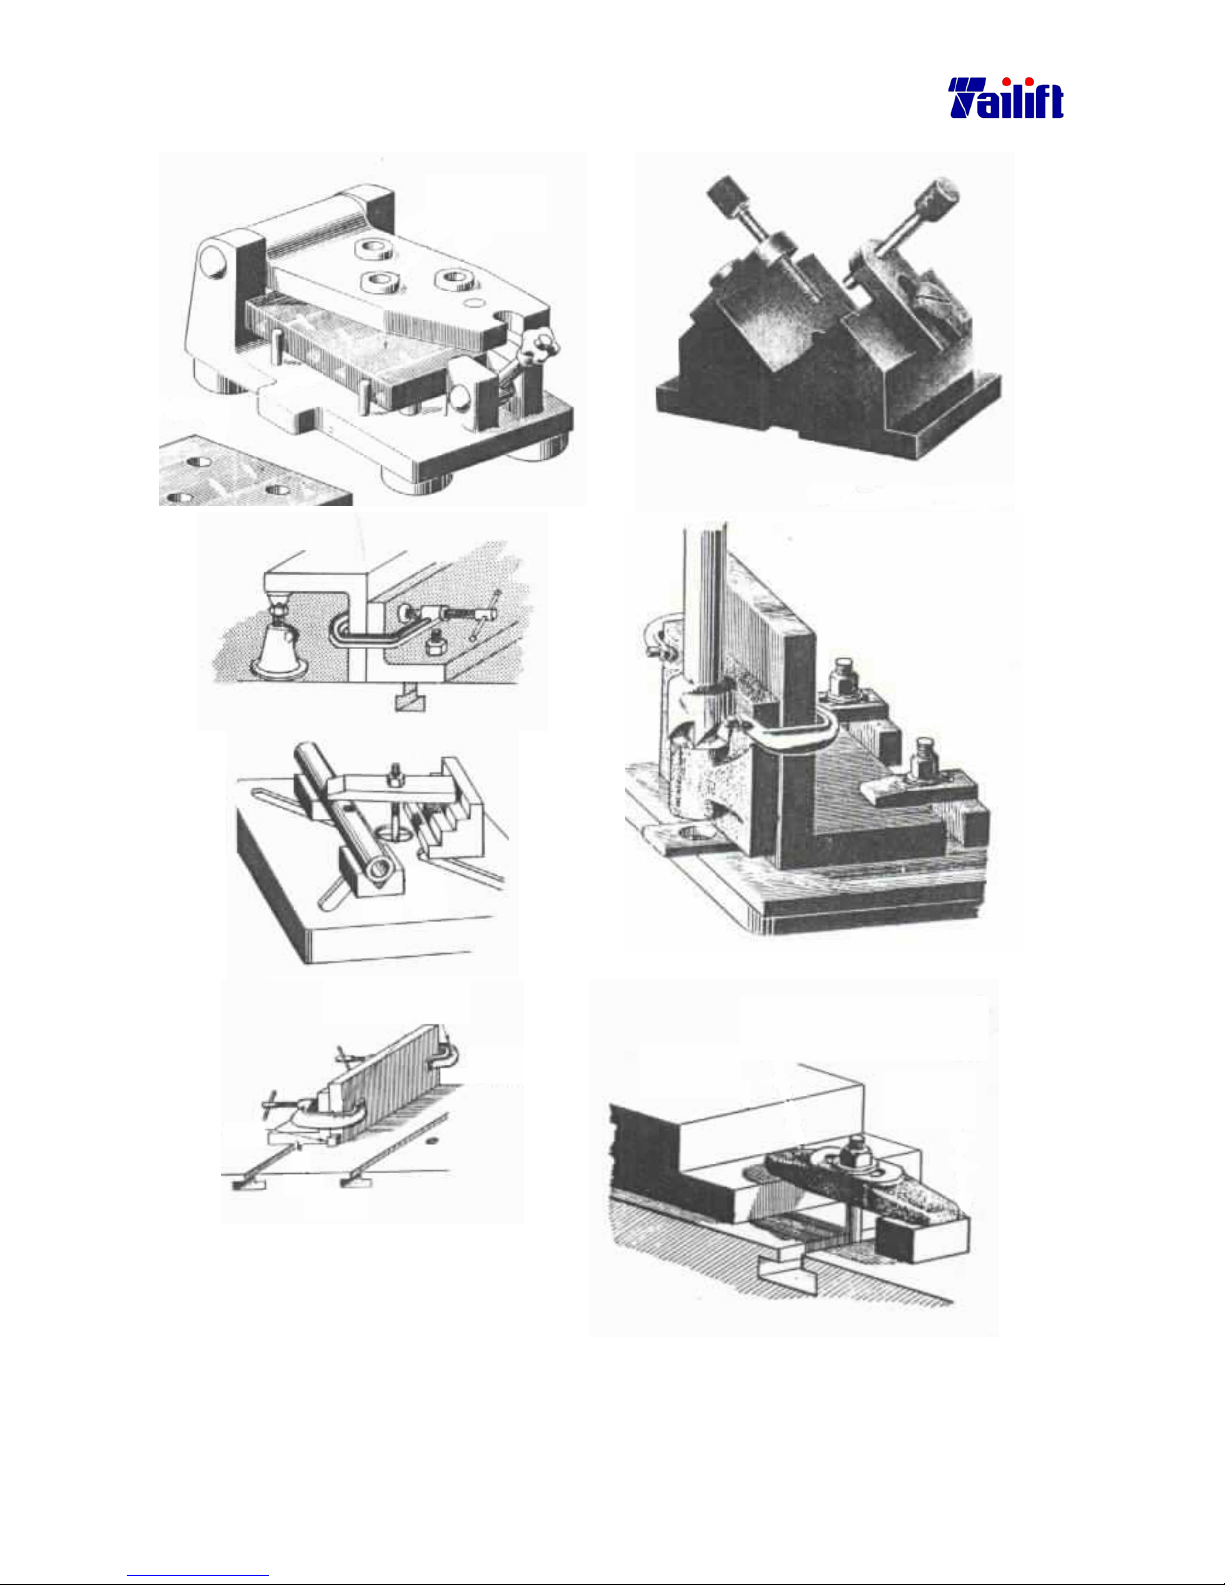
5-14
Examples of clamping, using the universal clamp.
Page 41
5-15
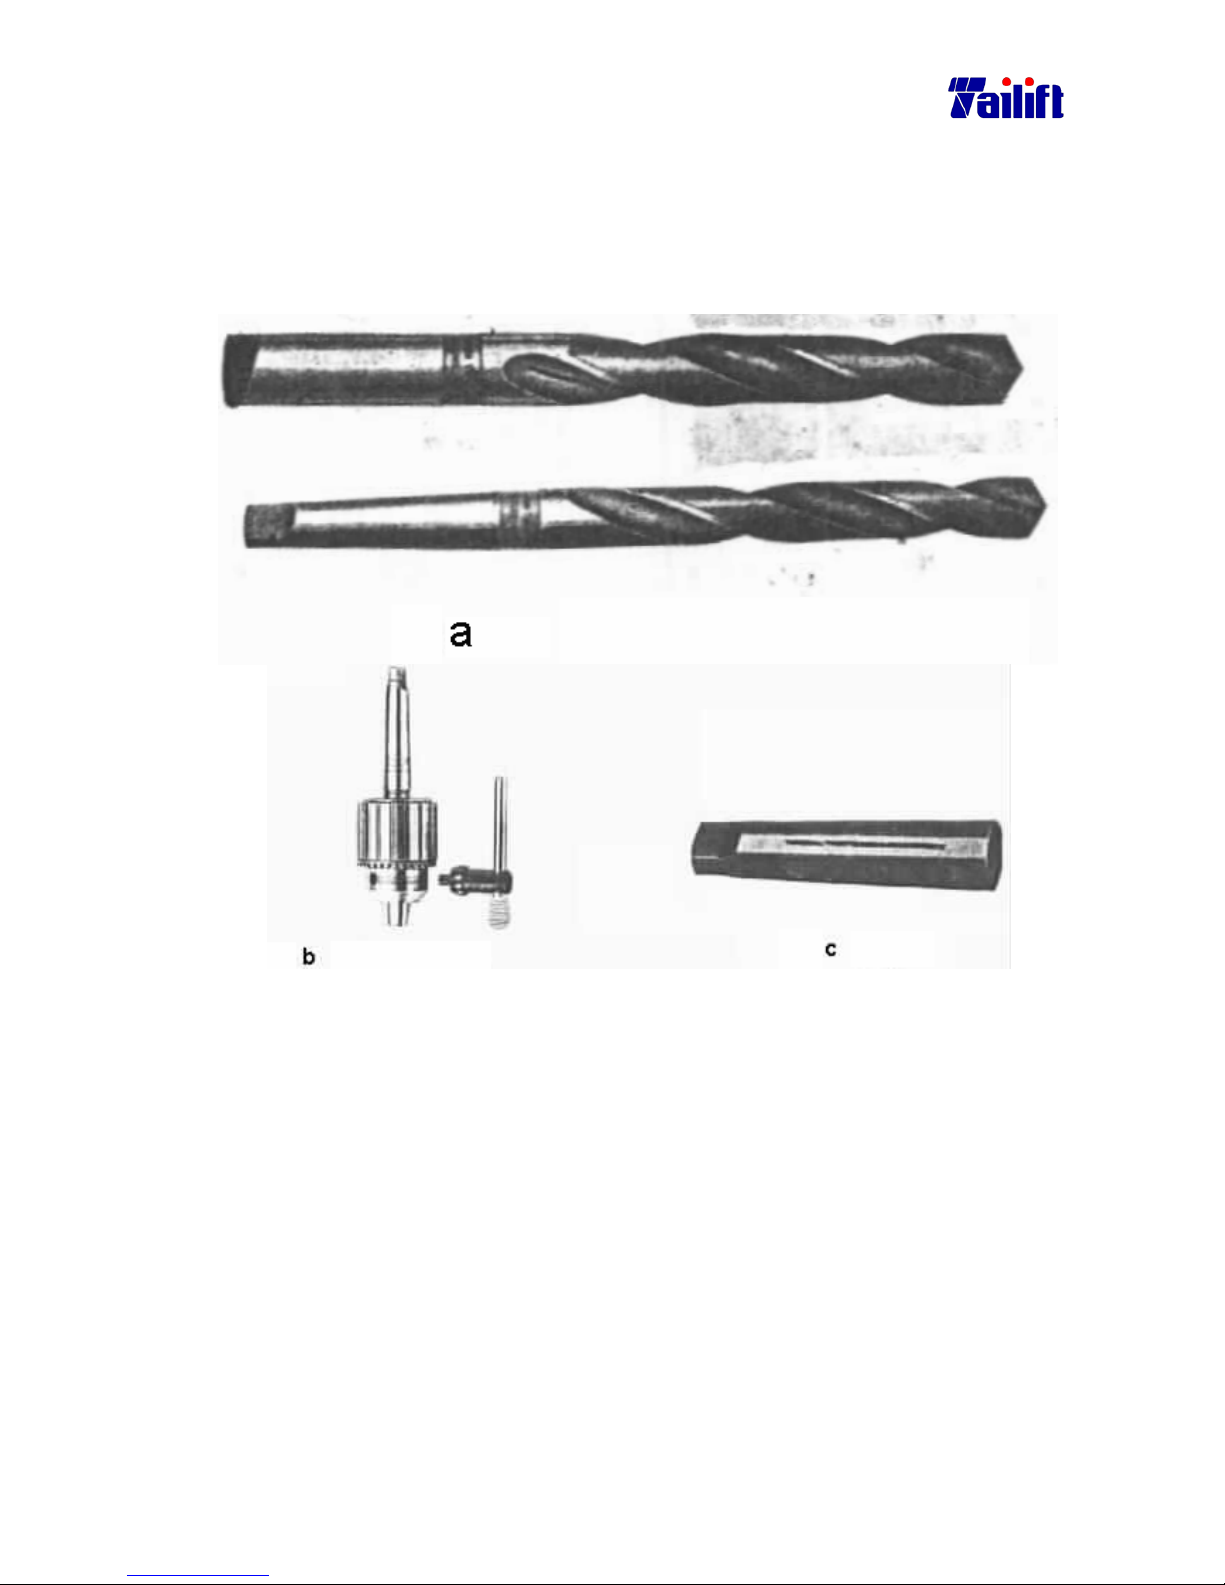
5.4 Installation and change of the drilling unit.
The radial drill is mainly used in drilling. How to clamp the drilling bit is therefore
very important. Generally, drilling bits divides into two kinds, one is straight handle
drilling bit, and another is tapered handle one. (as fig. A). Their clamping is very
different. The straight handle one is fixed by a drilling head while the tapered handle
one is
fixed by a bushing.
Page 42
5-16
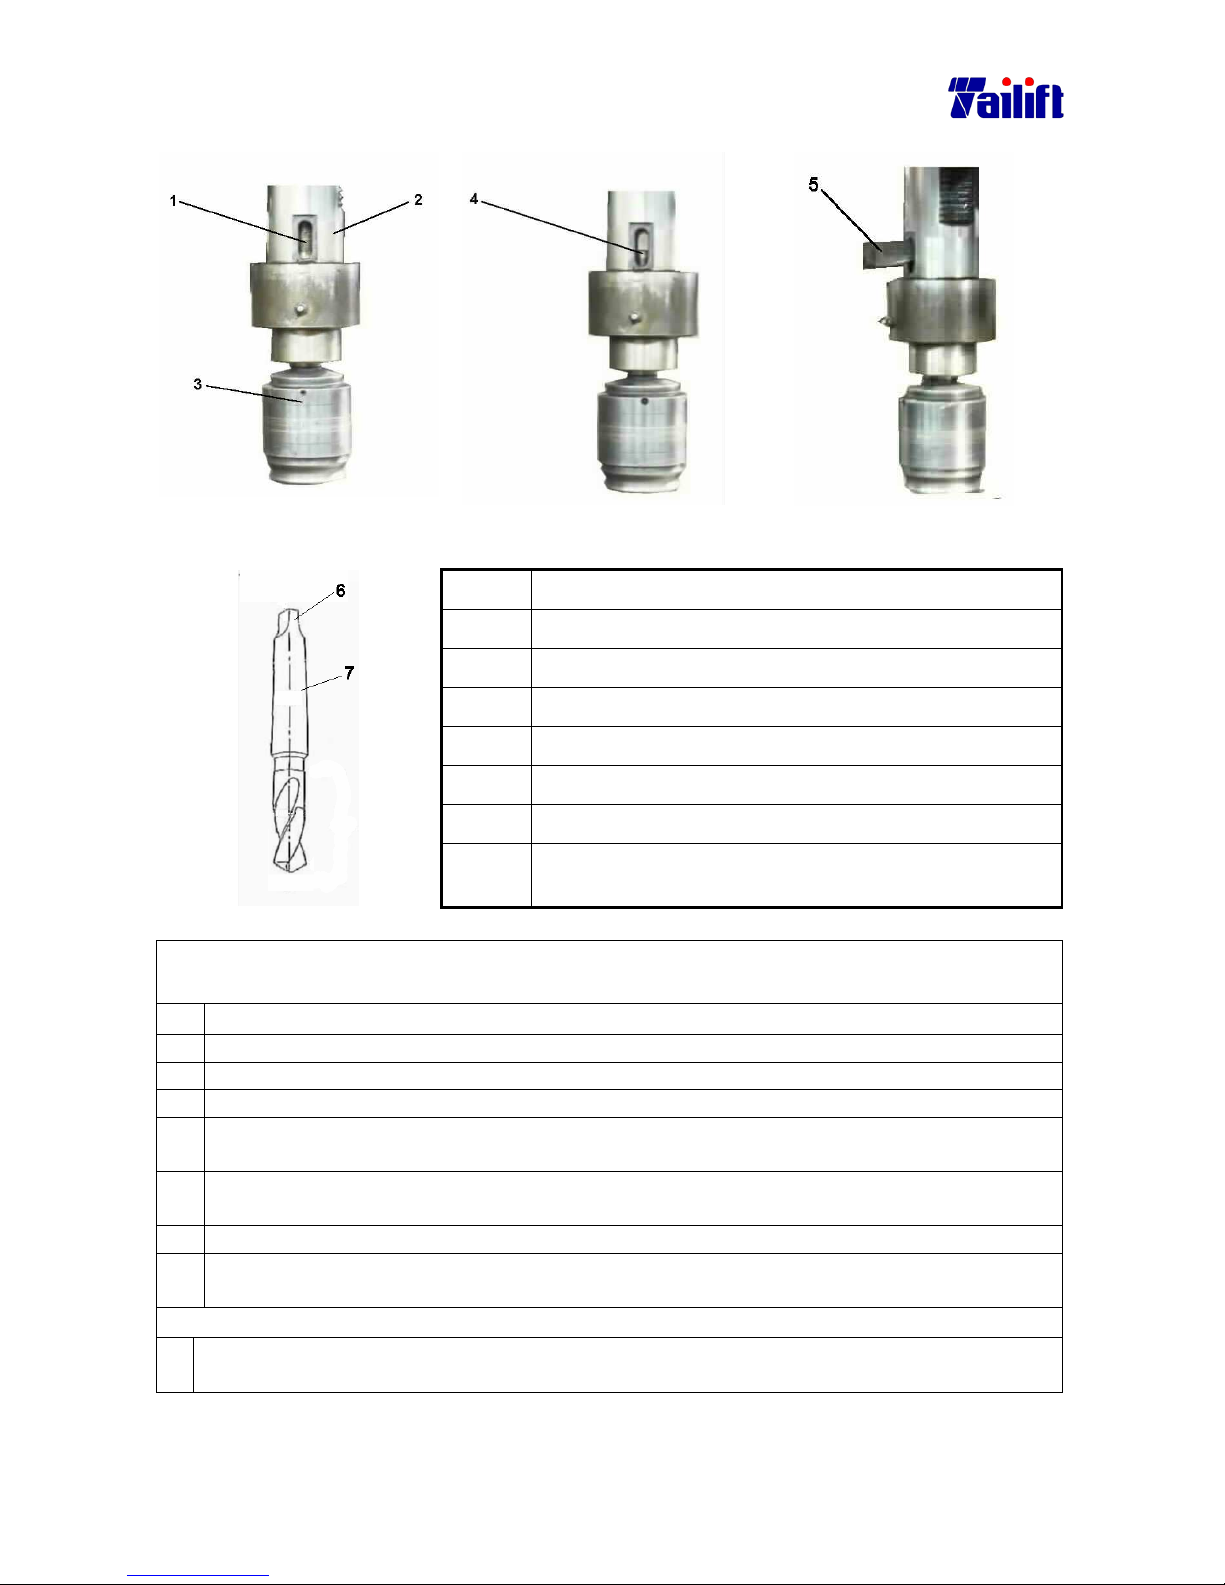
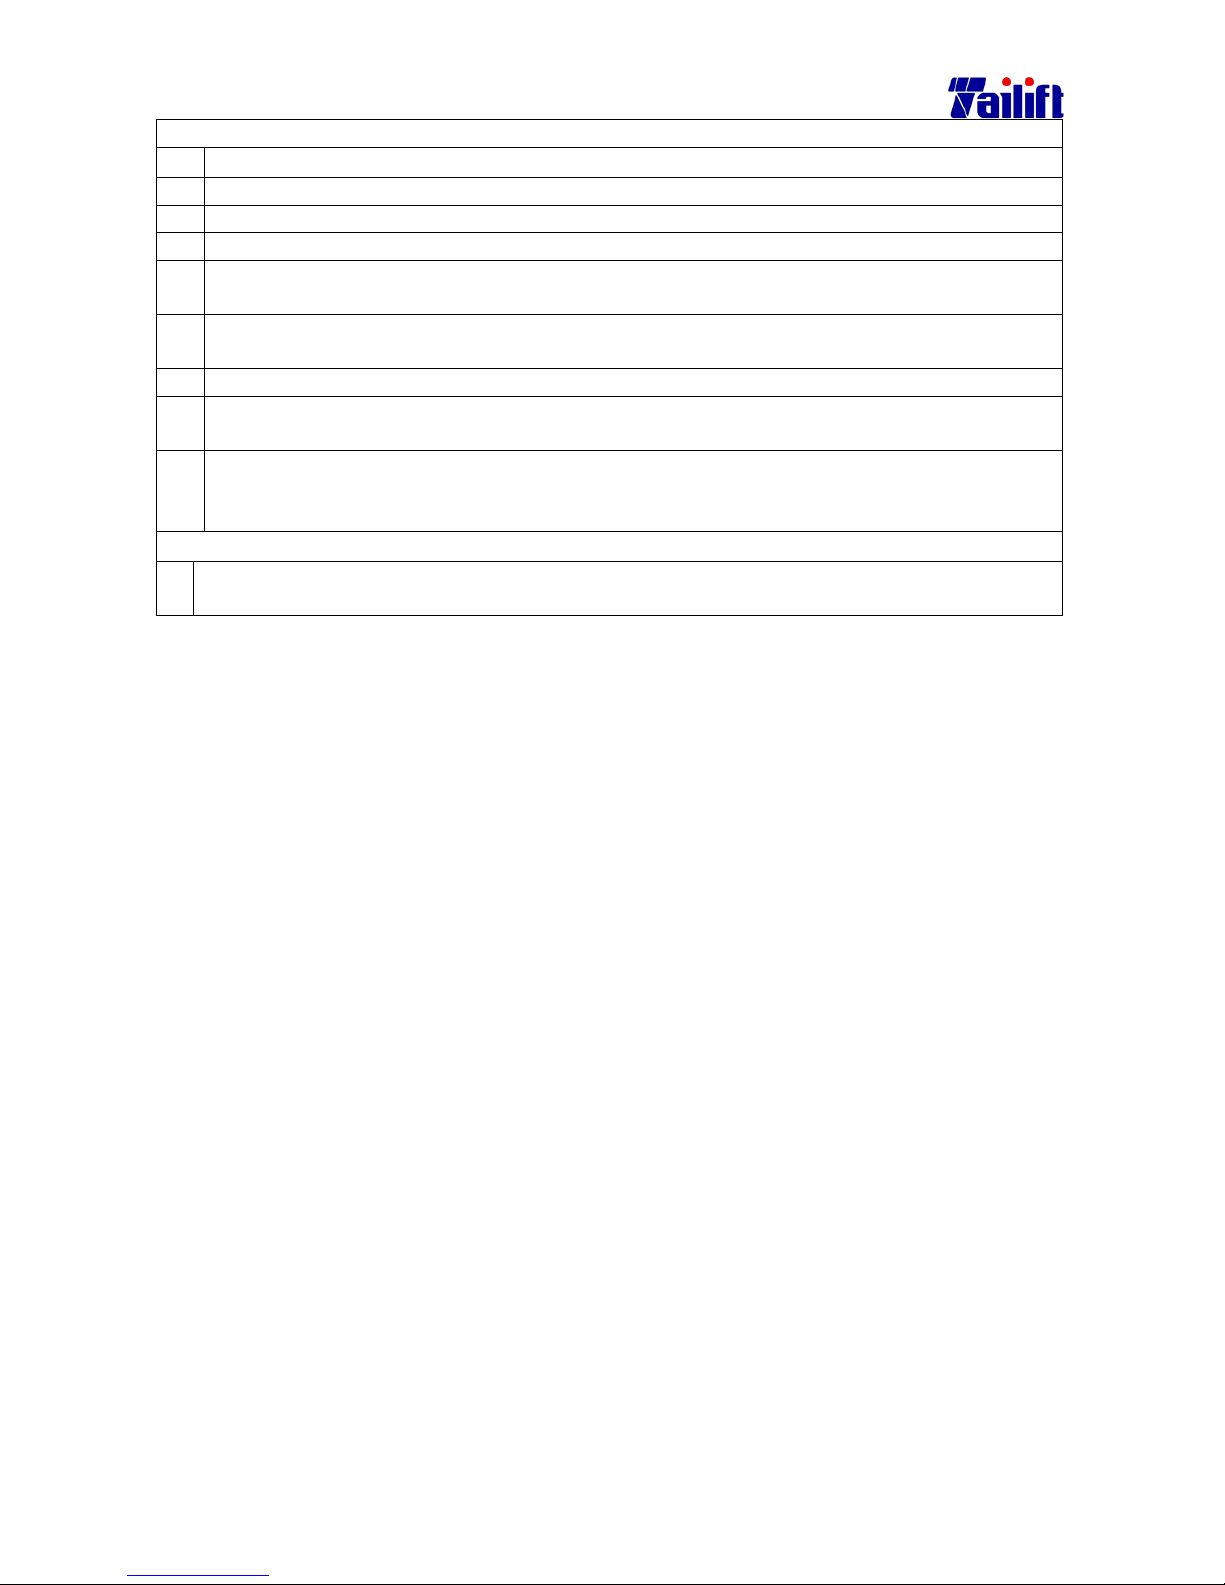
5.4.1 The assembly and disassembly of the drilling head and clamp
Fig. a. Fig. b. Fig. c.
No. Term
(1) Revolving shaft.
(2) Shaft bushing
(3) Speedy drill bit clamp
(4) The stem for the speedy drill bit clamp
(5) Pin for releasing drill bit
(6) Drill shaft end
(7) Drilling shaft
Fig. d.
Disassemble the tapered handle drill bit and the drill head clamp as the
following way:
a. Move away the drilling bit or lift the gearbox to the utmost point.
b. Power off machine.
c. Put on gloves.
d. Insert a thick wood plate into the underneath of the drill bit and the drill bit head.
e. Rotate the feed trip lever clockwise and have the spindle descend about
150 to 200 mm. As fig. a.
f. Rotate the revolving shaft from the bushing till that the drill shaft end and drill shaft
are visible from the hole of releasing drill bit. as fig. b.
g. Insert the pin for releasing the drill bit into the hole, as fig. c.
h. Hit the end of the pin for releasing drill bit, using plastic hammer or copper bar, till the
drill bit and the drill bit clamp fall onto the wood plate.
Precaution::::
The distance between the thick wood plate, drill bit and the end of the drill bit clamp is
about 30 mm.
Page 43
5-17
Assemble the drill bit head and the drill bit clamp as the following:
a. Move away the drilling bit or lift the gearbox to the utmost point.
b. Power off.
c. Put on gloves.
d. Insert a thick wood plate into the underneath of the drill bit and the drill bit clamp.
e. Rotate the feed trip lever clockwise and have the spindle descend about
150 to 200 mm. As fig. a.
f. Rotate the revolving shaft from the bushing till that thing behind the machine is visible
from the hole of releasing drill bit, as fig. b.
g. Place the drill bit clamp end up, as fig. d.
h. Place the drill bit and its clamp end into the revolving shaft and have the drill shaft end
inserted into the hole for releasing the drill bit, as fig. b.
i. Rotate the feed trip lever counter clockwise. Make the spindle descend till the drill bit
and the bottom end of the drill bit clamp head contact the wood plate. Apply a little bit
force and complete it by confirming that the drill bit won’t fall.
Precaution::::
The distance between the thick wood plate, drill bit and the end of the drill bit clamp is
about 30 mm.
Page 44
5-18
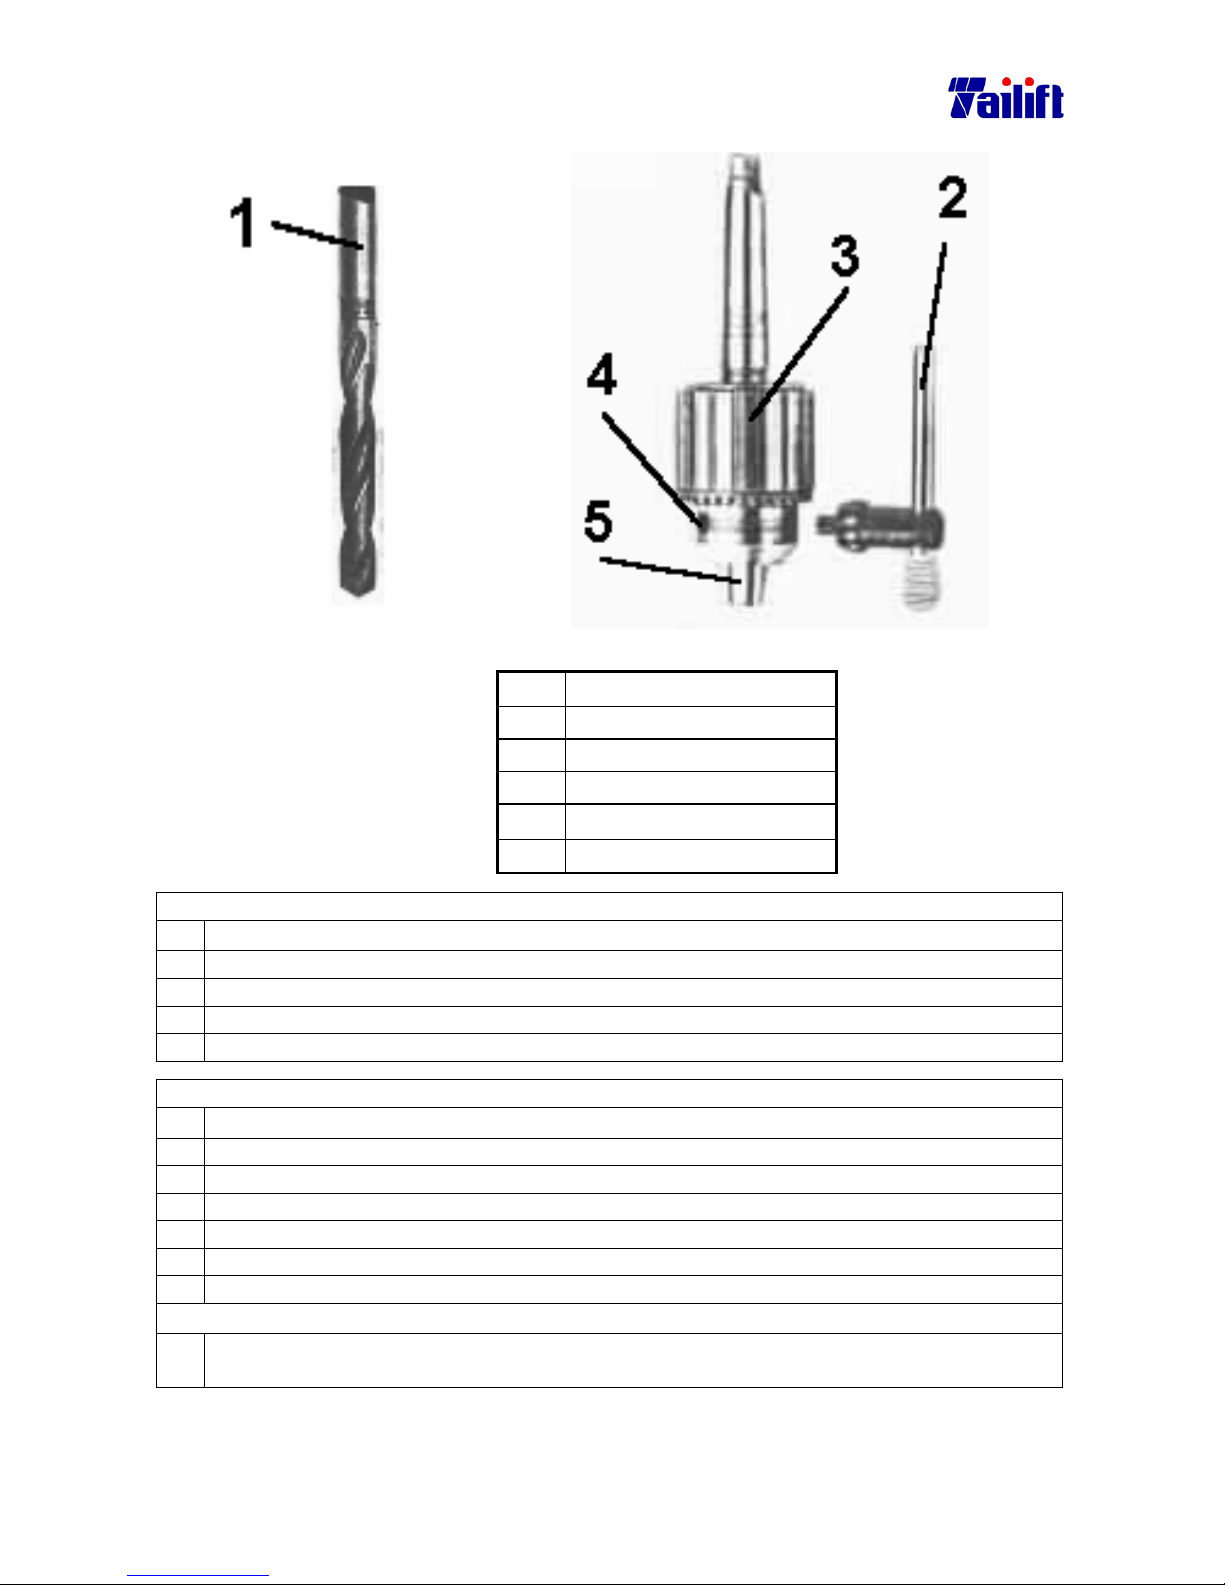
5.4.2 The assembly and disassembly of the straight handle drill bit
Fig. a. Fig. b.
No. Term
(1) Drill bit
(2) Drill spanner
(3) Tightening ring
(4) Hole for drill spanner.
(5) Drill bit clamp head.
Disassemble the straight drill bit as the following way:
a. Move away the drilling bit or lift the gearbox to the utmost point.
b. Power off.
c. Put on gloves.
d. Put the drill spanner into the hole for tightening.
e. Rotate the spanner counter clockwise till the clamp head falls.
Assemble the straight handle drill bit as the following way:
a. Move away the drilling bit or lift the gearbox to the utmost point.
b. Power off.
c. Put on gloves.
d. Adjust the tightening ring till the drill bit can be inserted.
e. Insert the drill bit into the clamp head at least 25 mm.
f. Put the drill spanner into the hole for tightening.
g. Rotate the spanner clockwise till the drill bit is tightened.
Precaution::::
The drill bit must be inserted at least over 25 mm, otherwise the bit get easily broken or
can’t drill very precisely.
Page 45
5-19
5.5 Power on and off.
5.5.1 Power on
a. Turn outside main switch to ”ON” position.
b. Turn the machine power switch to ”ON” position.
5.5.2 Power off
a. Turn the machine power switch to ”OFF” position.
b. Turn outside main switch to ”OFF” position.
Precaution When at emergency, please press down the emergent stop button to shut
down the power supply.
But the emergent stop button can’t be used as a switch for normally
stopping machine or normal power off.
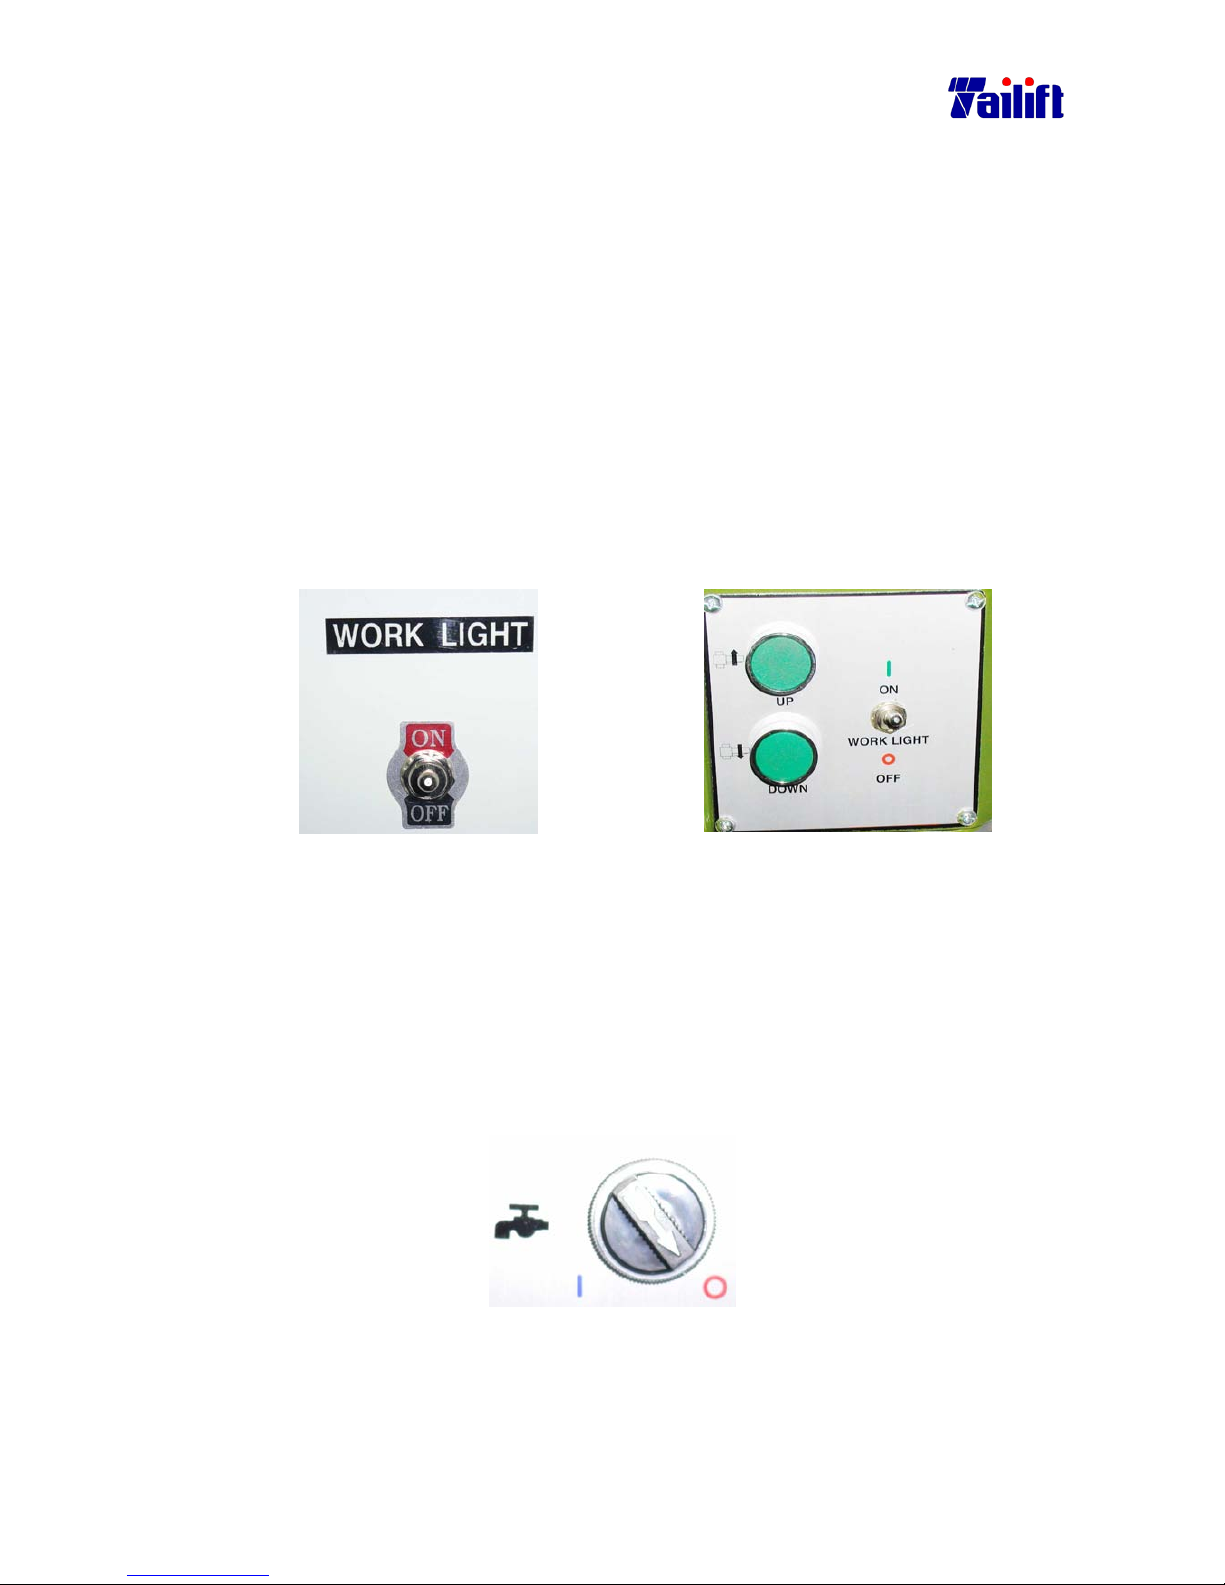
5.6 Work light
Turn on the work light. Switch the work light to ”ON” position.
Turn off the work light. Switch the work light to ”OFF” position.
For TPR720.TPR820.TPR920.TPR1100 For TPR1100(二二二二)
5.7 Cutting fluids
Turn on the cutting
fluids.
Switch the cutting fluids to ”ON” position.
Turn off the cutting
fluids.
Switch the cutting fluids to ”OFF” position.
Page 46
5-20
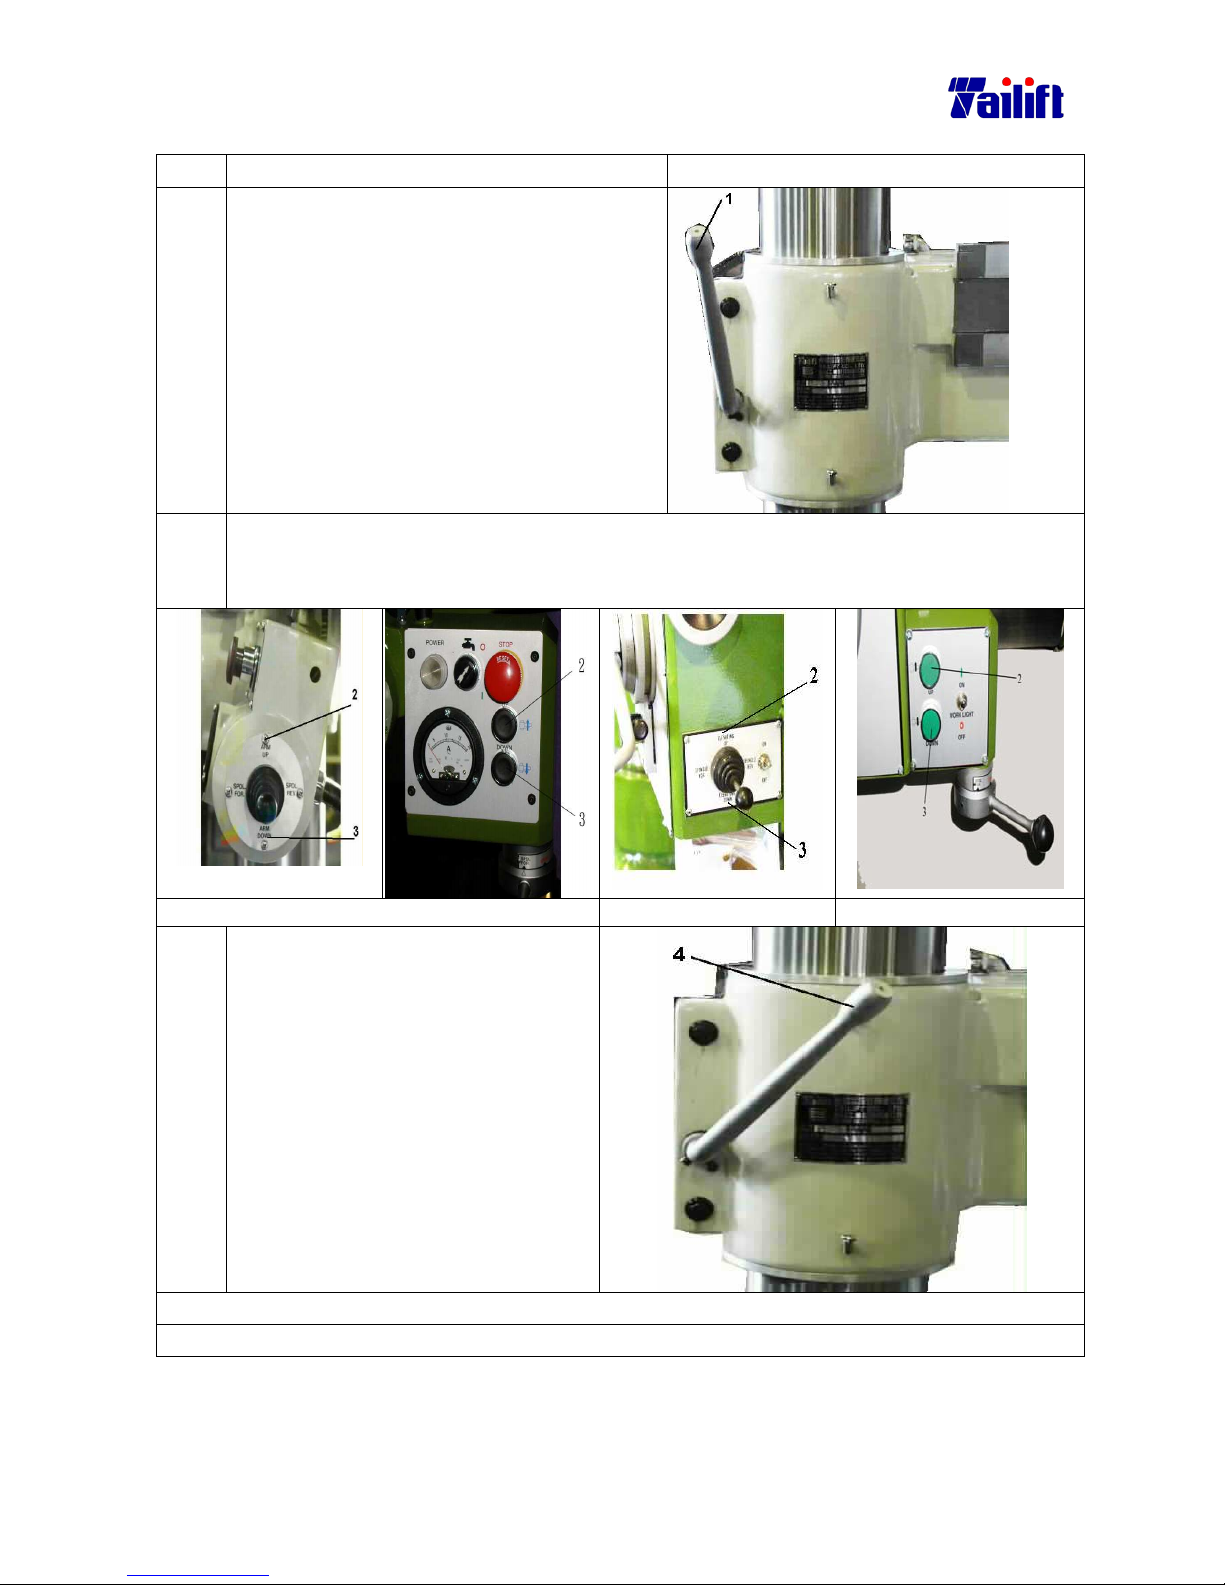
5.8 Elevating the arm.
Steps
Description Diagrams
1. Revolve the arm clamping lever counter
clockwise to loosen it as shown in fig. 1.
2.
Please switch up the “cross switch” or push the “up” button shown as
the Picture on the right hand . Shown No.2 Please switch down the
“cross switch” or Push the “down”button No3. Arm down or down.
(For TPR-720A,TPR-820A,TPR-920A) (For TPR1100)( Type I) (For TPR1100)( Type I)
3. Revolve the arm clamping lever
clockwise to tighten it as shown
in fig. 4.
Precaution
You can’t either ascend or descend the arm when it is clamped.
Page 47
5-21
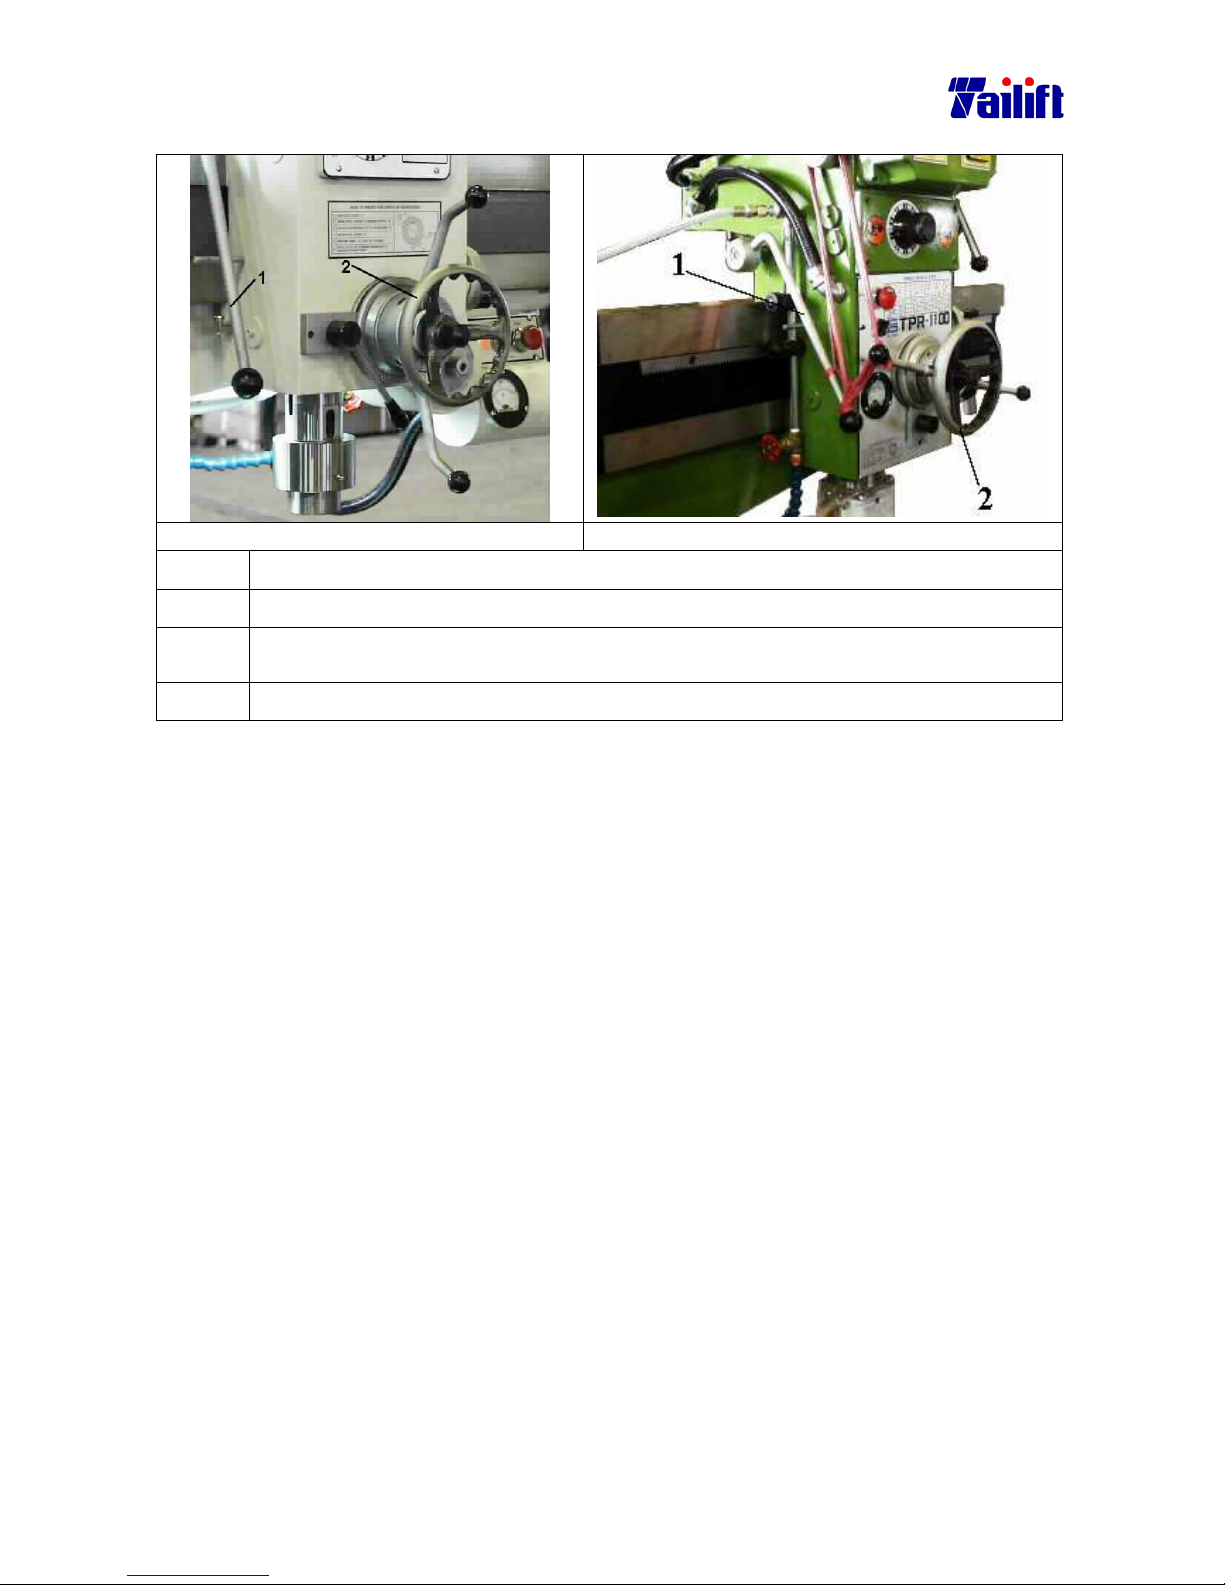
5.9 Rotate the arm right or leftwards.
(For TPR-720A, TPR-820A, TPR-920A) (For TPR-1100)
Steps Description
1. Push the head lever downwards to release, as shown in picture 1.
2.
Rotate the hand wheel clockwise to move rightwards and counter clockwise to move
leftwards, as shown in picture 2.
3. Pull the head lever upwards to tighten the head, as shown in picture 1.
Page 48
5-22
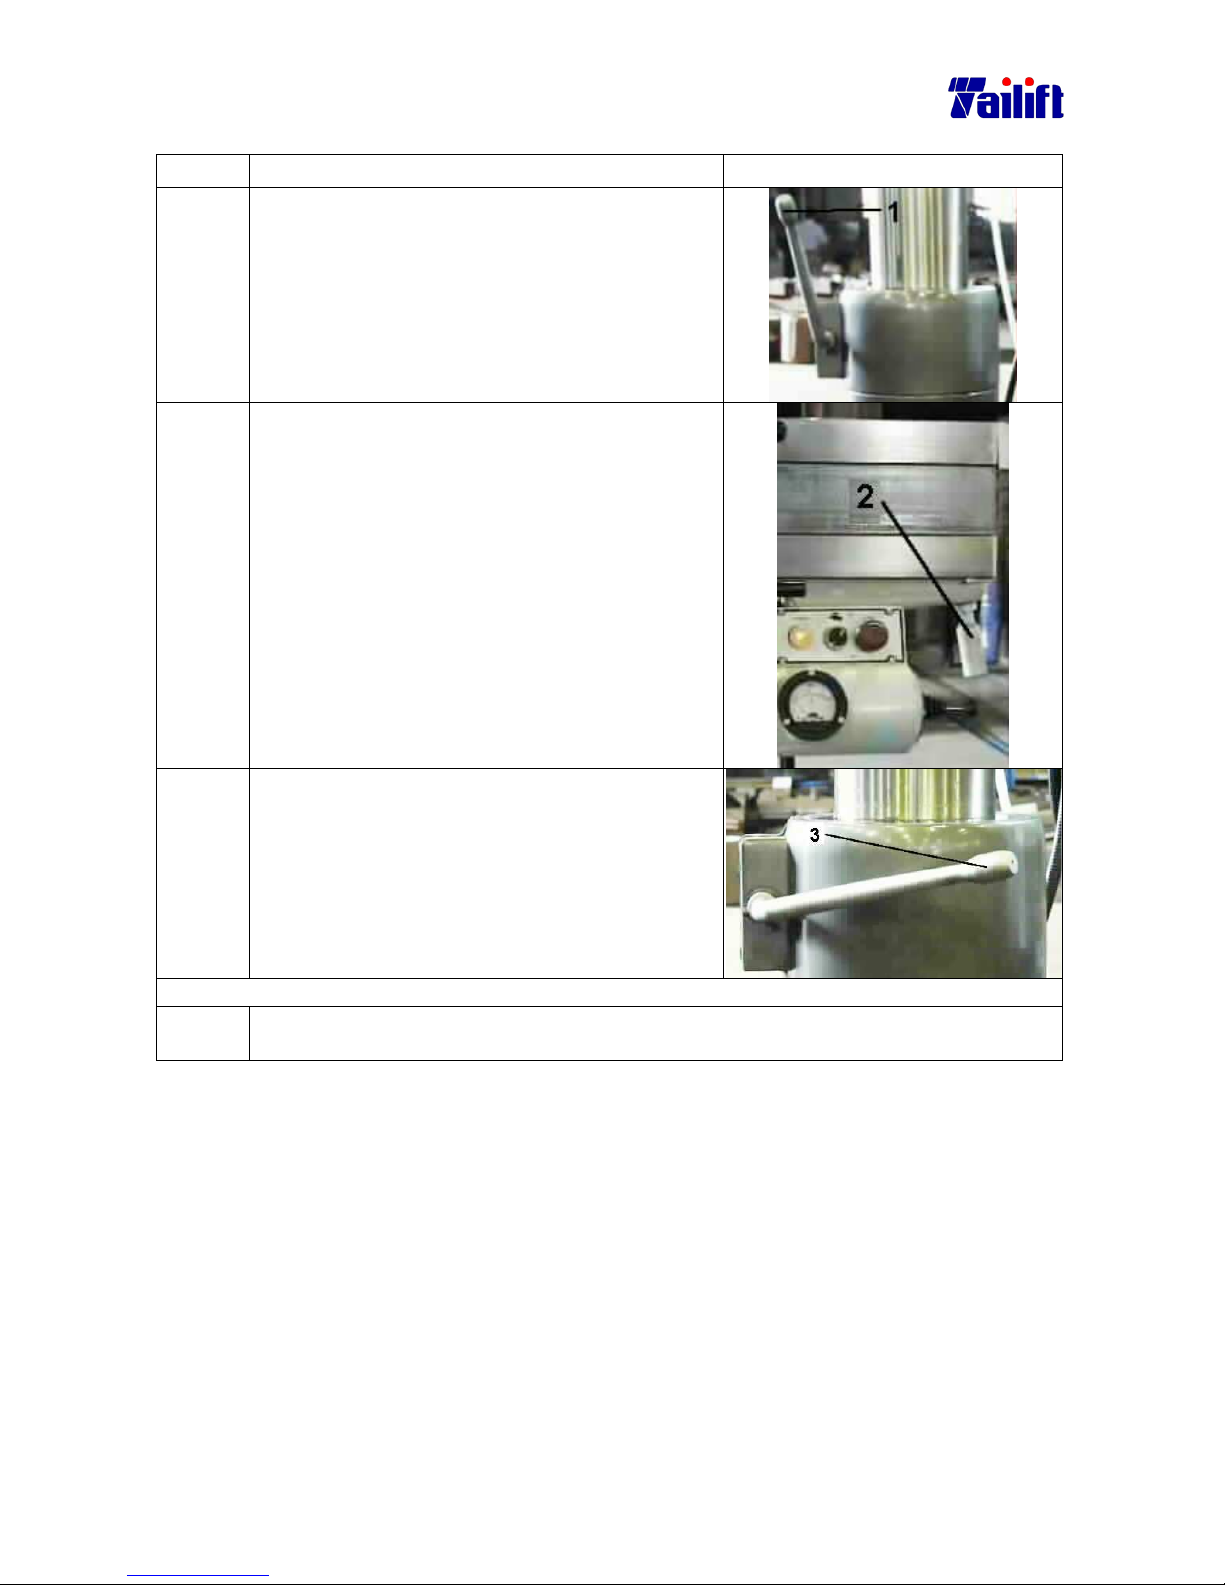
5.10 Rotate the arm forward or backwards.
Steps
Description Diagrams
1. Rotate the arm clamping lever counter
clockwise to release it, as shown in picture 1.
2.
Push the arm moving lever backwards to move
the arm backwards, as shown in picture 2. Pull
the arm moving lever towards to move the arm
towards, as shown in picture 2.
3. Rotate the arm-clamping lever clockwise to
tighten the arm-clamping lever, as shown in
picture 3.
Precaution
If turning 180 degree is needed, the ground base needs to be processed according to
the principles of the chapter 3 and fastened with nuts.
Page 49
5-23
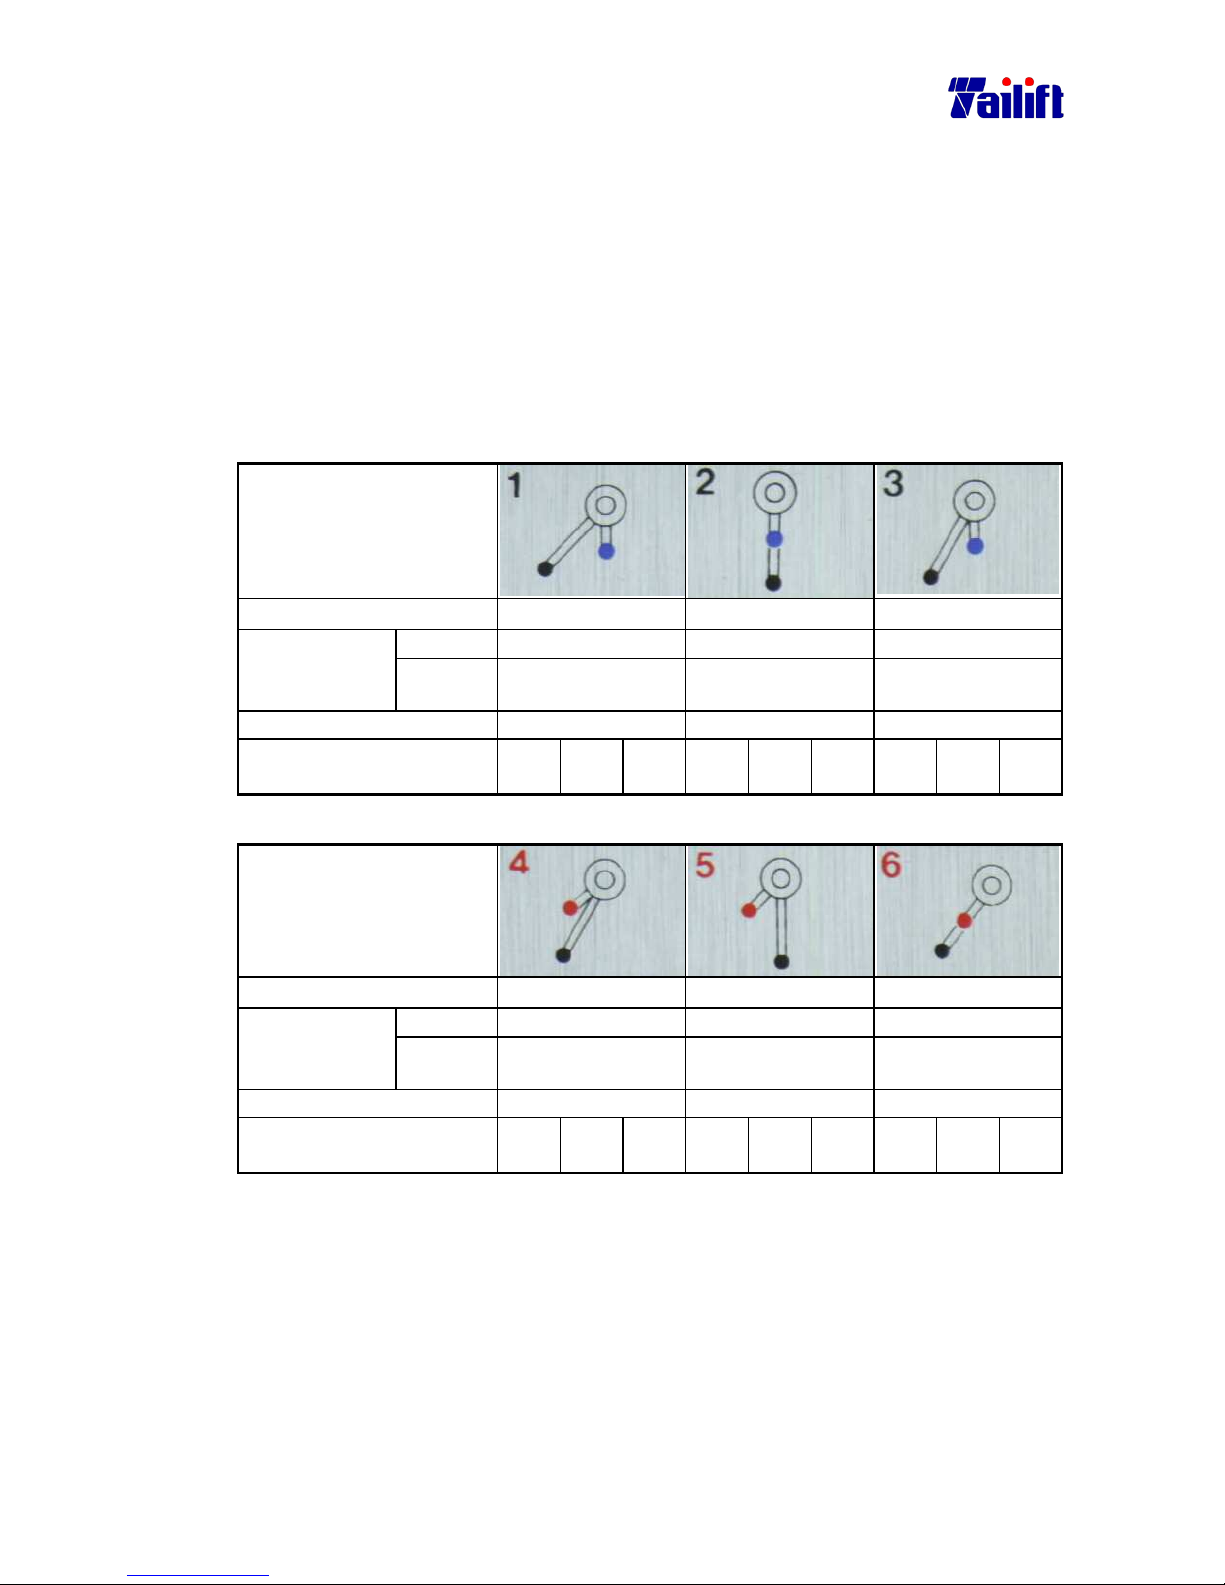
5.11 Change the spindle speed.
Warning :
Spindle temperature will go up making operation in trouble when the
spindle speed is set at high rotation mode without movement of the
quill. So please do not set the spindle speed at high rotation mode
when no movement of the quill.
5.11.1 For TPR-720A, TPR-820A, TPR-920A
Ⅰ
ⅠⅠ
Ⅰ. Speedometer
Two speed change lever((((low speed))))
Speed change levels
Speed((((rpm)))) 88 154 282
Mild steel
∅∅∅∅25-∅∅∅∅32 ∅∅∅∅19-∅∅∅∅25 ∅∅∅∅12-∅∅∅∅19
Suitable
drilling
diameter mm
Cast iron
∅∅∅∅38-∅∅∅∅50 ∅∅∅∅28-∅∅∅∅38 ∅∅∅∅22-∅∅∅∅28
Threading (metric) M16-M22 M6-M16 M3-M6
Suitable automatic
feeding step.
1 2 3 1 2 3 1 2 3
Two speed change lever((((high speed))))
Speed change levels
Speed((((rpm)))) 455 796 1500
Mild steel
∅∅∅∅10-∅∅∅∅12 ∅∅∅∅6-∅∅∅∅10 ∅∅∅∅3-∅∅∅∅6
Suitable
drilling
diameter mm
Cast iron
∅∅∅∅19-∅∅∅∅22 ∅∅∅∅10-∅∅∅∅19 ∅∅∅∅3-∅∅∅∅10
threading(metric) Not suggested. Not suggested. Not suggested.
Suitable automatic
feeding step.
1 2 3 1 2 3 1 2 3
Page 50
5-24
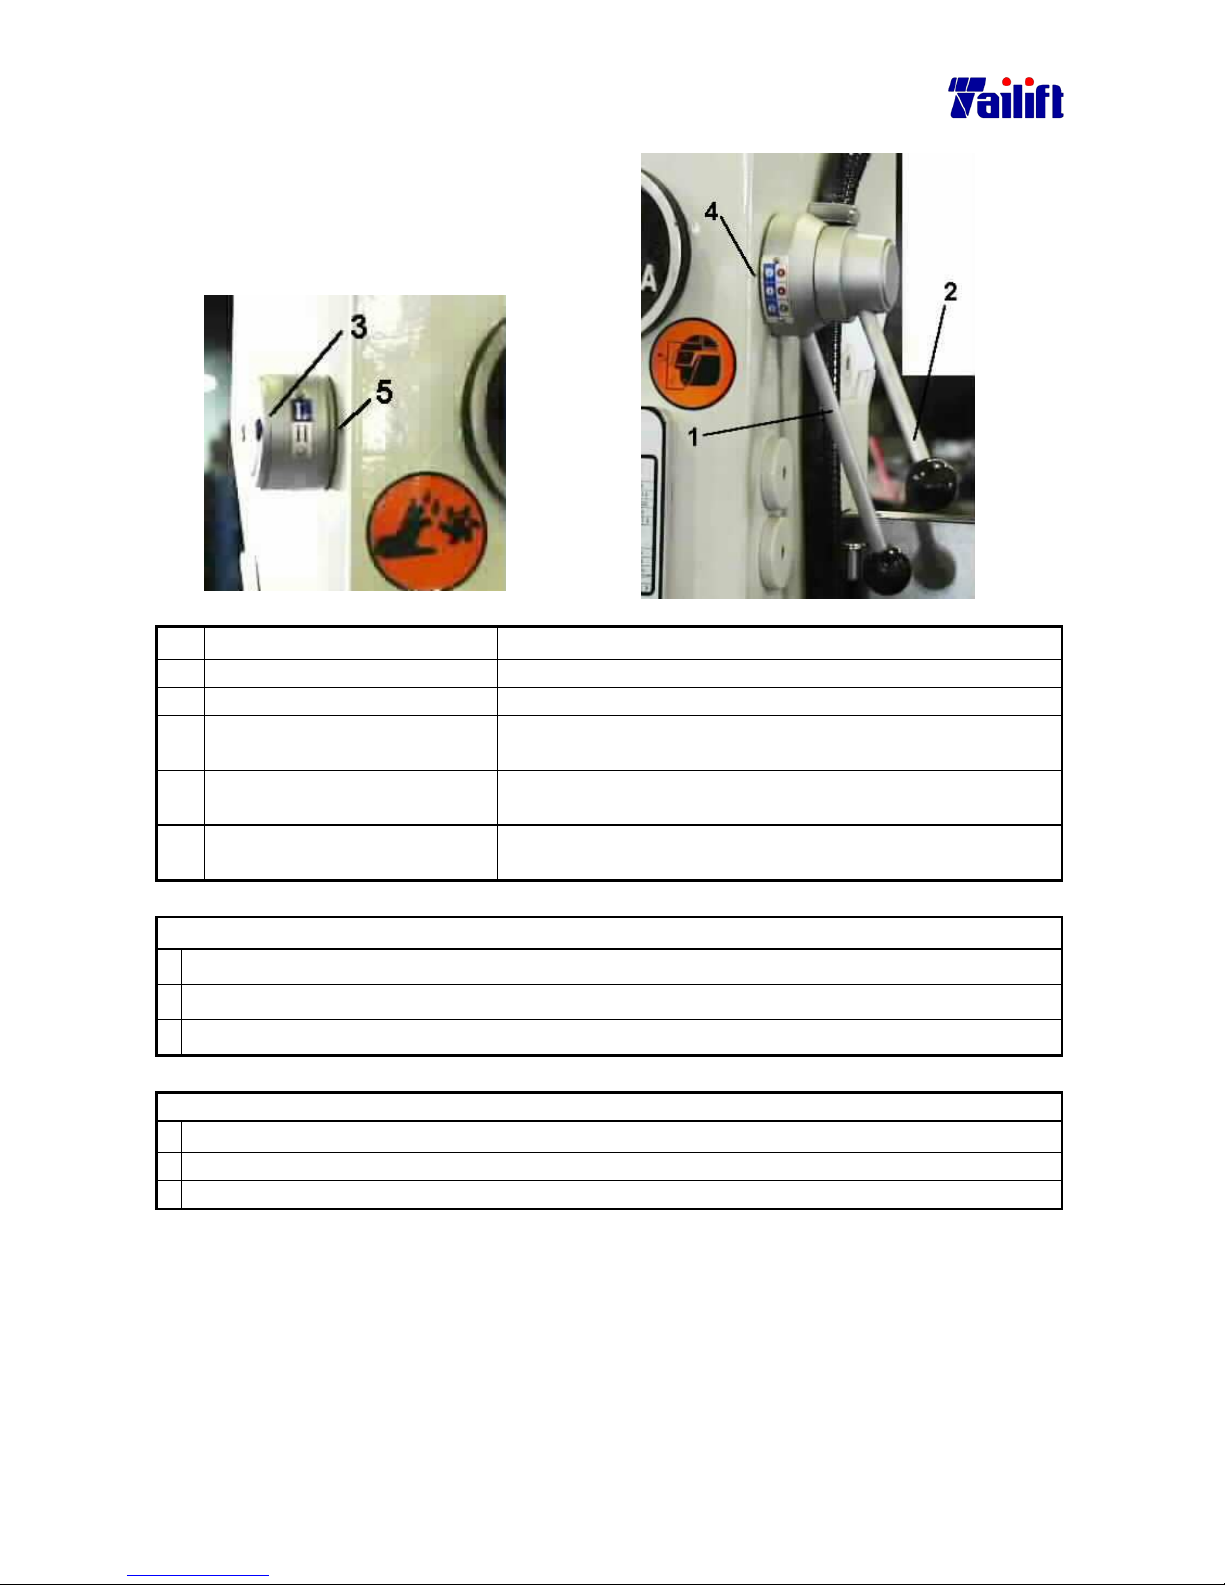
Ⅱ
ⅡⅡ
Ⅱ. Change spindle speed
Pic. a. Pic. b.
No.
Term Description
1. Three speeds change lever
2. Two speeds change lever High and low speeds change lever.
3. Indicating ring for high and
low speed.
It is to indicate the current speed.
4. Reference point for the three
speeds change lever
It refers to the current position of the three speeds change
lever.
5. Reference point for the two
speeds change lever
Ⅲ
ⅢⅢ
Ⅲ. Change the spindle speed as the following way:
a. Have spindle rotate.
b. Look up in the speed table and choose a suitable speed rate.
c. Turn on the switch for the feed rate.
Precaution when changing speed:
a. Spindle rotation must be stopped when at changing speed.
b. Please press down the emergent stop button for safety reason.
c. Change speed only after the spindle stops completely.
Page 51
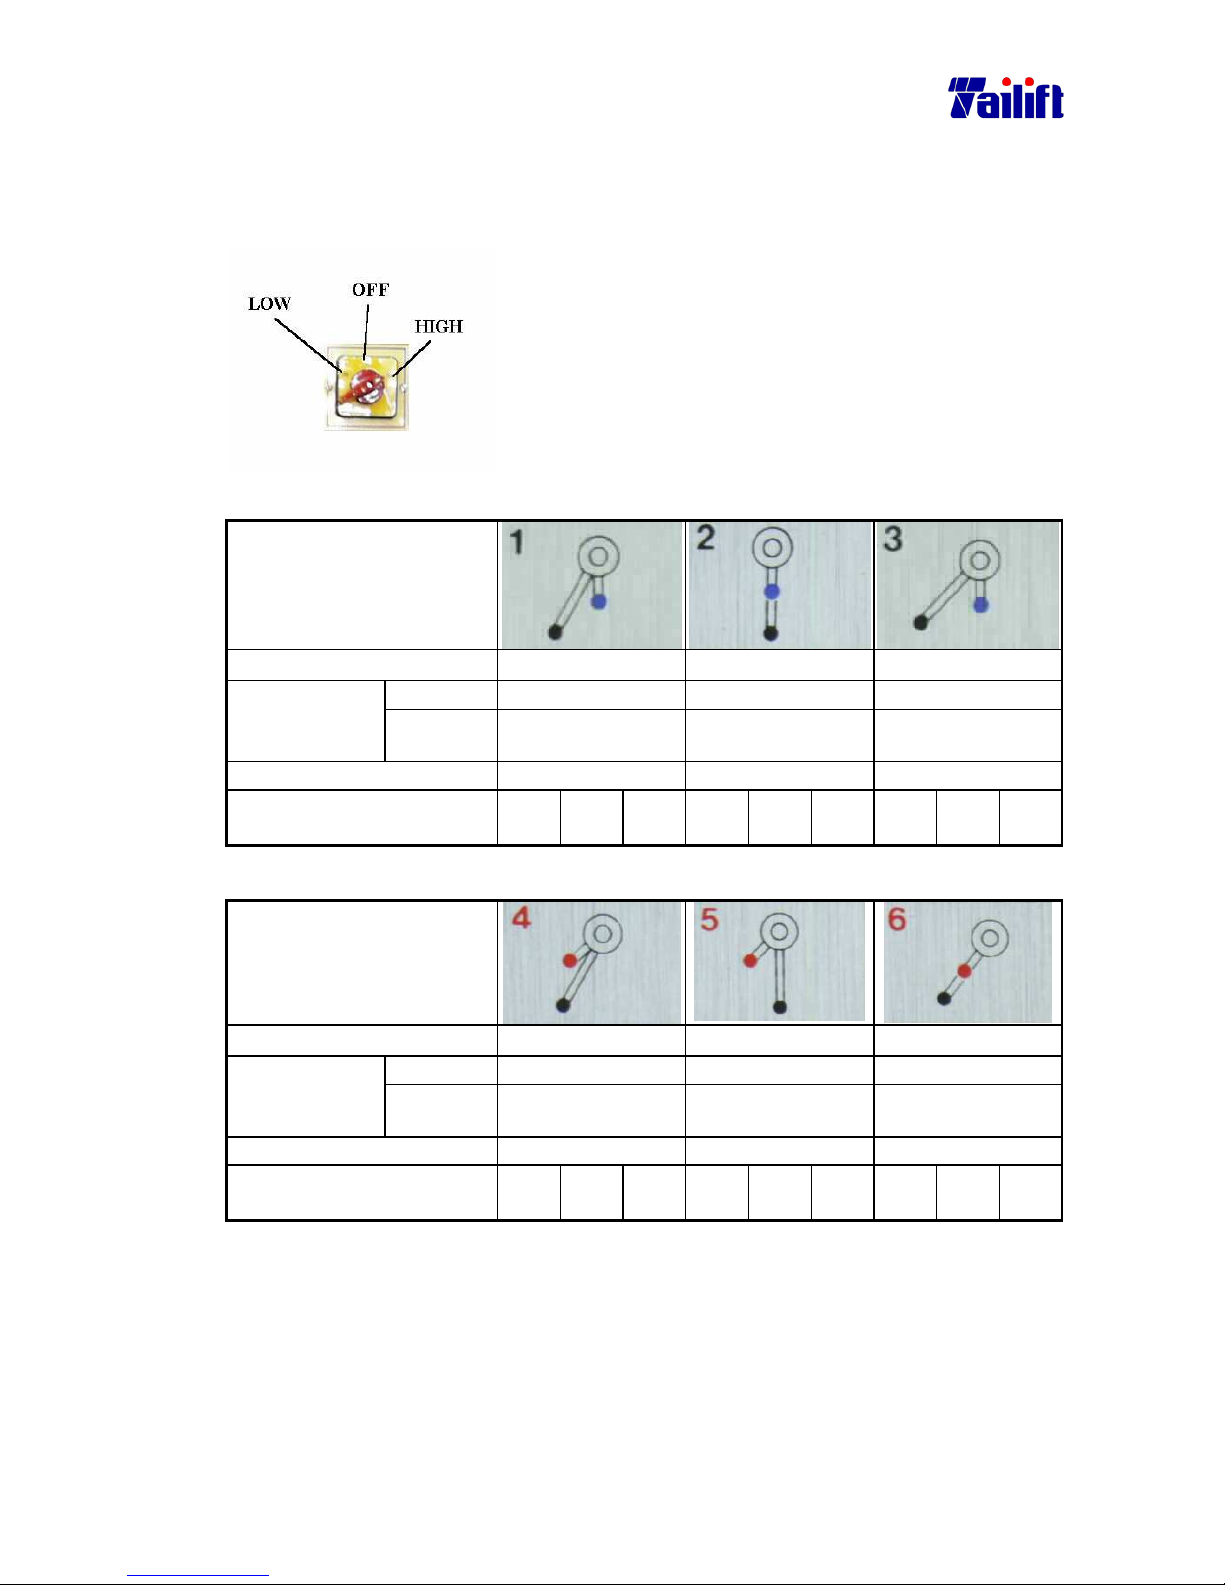
5-25
5.11.2 For TPR-1100
Ⅰ
ⅠⅠ
Ⅰ. The speedometer at the time
when the pole switch is in high position.
The position for the pole switch.
Two speed change lever((((low speed))))
Speed change levels
Speed((((rpm)))) 88 154 282
Mild steel
∅∅∅∅25-∅∅∅∅40 ∅∅∅∅19-∅∅∅∅25 ∅∅∅∅12-∅∅∅∅19
Suitable
drilling
diameter mm
Cast iron
∅∅∅∅38-∅∅∅∅55 ∅∅∅∅28-∅∅∅∅38 ∅∅∅∅22-∅∅∅∅28
Threading (metric) M16-M20 M6-M16 M3-M6
Suitable automatic
feeding step.
1 2 3 1 2 3 1 2 3
Two speed change lever((((high speed))))
Speed change levels
Speed((((rpm)))) 456 796 1500
Mild steel
∅∅∅∅10-∅∅∅∅12 ∅∅∅∅6-∅∅∅∅10 ∅∅∅∅3-∅∅∅∅6
Suitable
drilling
diameter mm
Cast iron
∅∅∅∅19-∅∅∅∅22 ∅∅∅∅10-∅∅∅∅19 ∅∅∅∅3-∅∅∅∅10
threading(metric) Not suggested. Not suggested. Not suggested.
Suitable automatic
feeding step.
1 2 3 1 2 3 1 2 3
Page 52
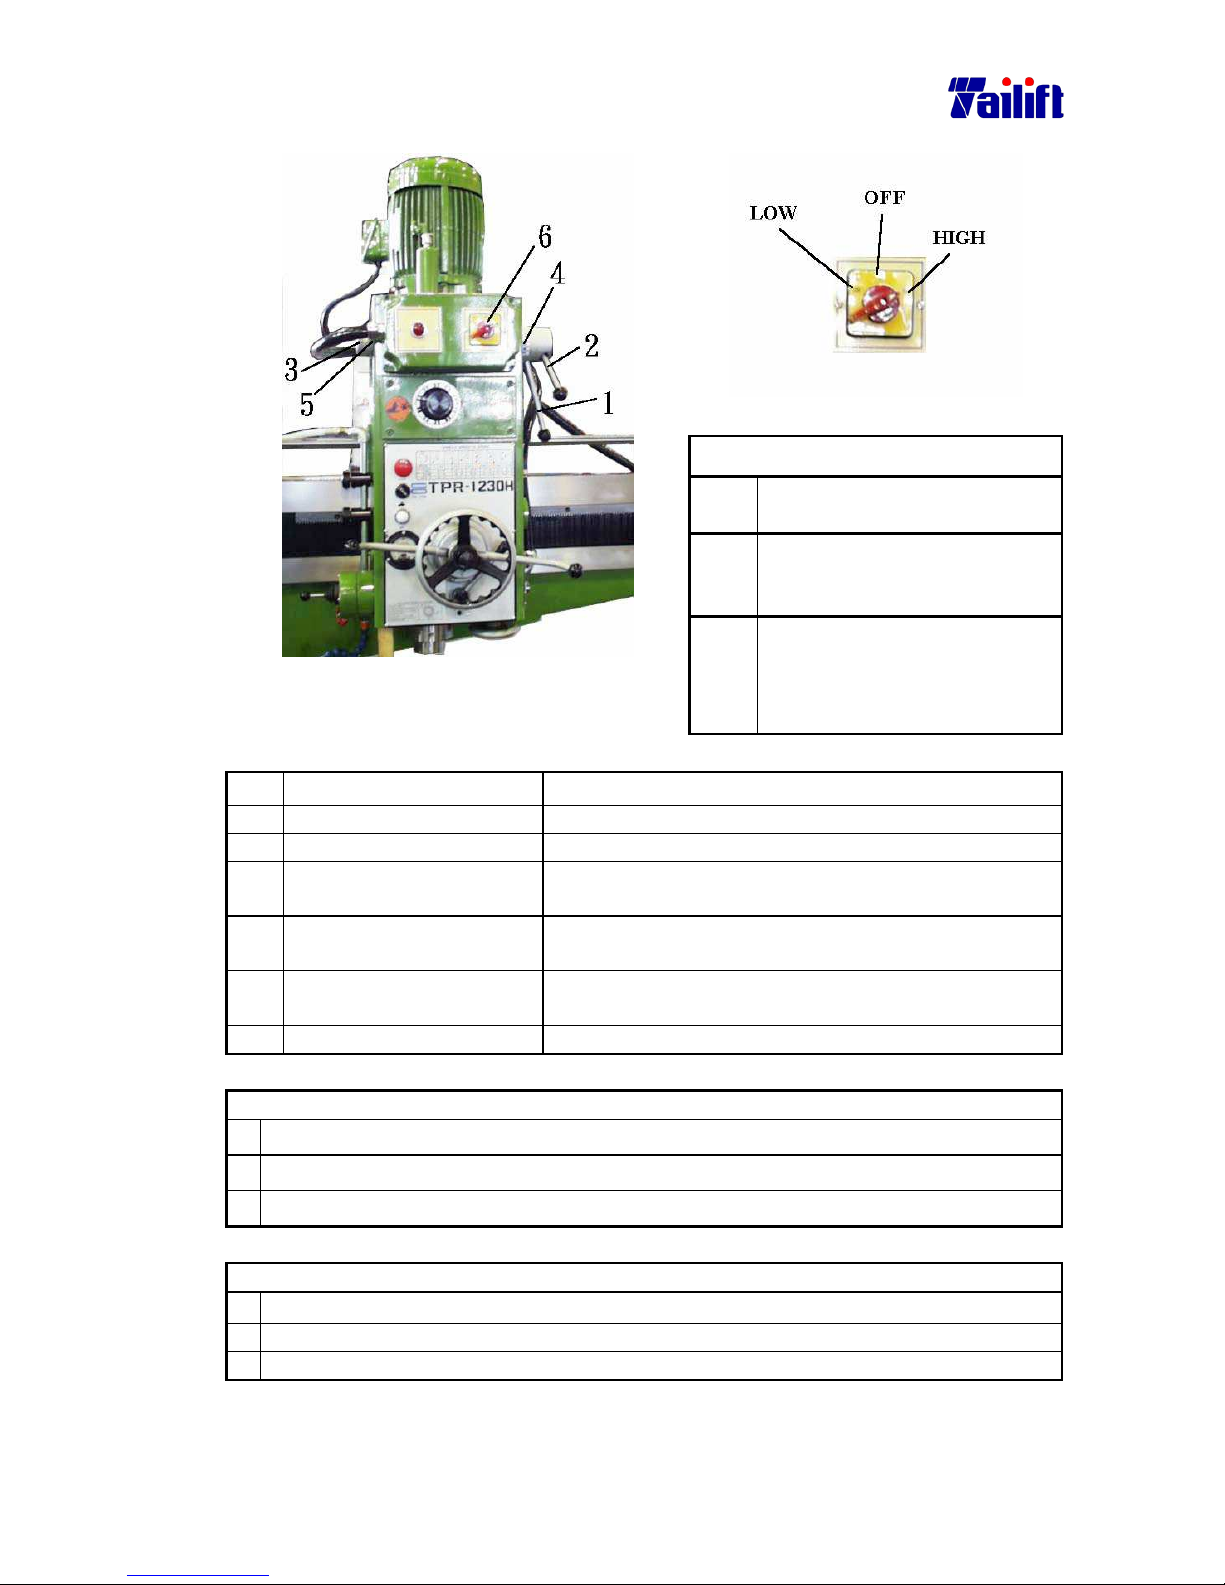
5-26
Ⅱ
ⅡⅡ
Ⅱ. Change spindle speed
Pic. b.
Label 6 of detail
Low
If the pole switch to high
position, its 8 pole.
OFF
If the pole switch to “OFF”
posit
ion, the motor can’t turn
run.
Pic. a.
High
If the pole switch in high
position, its 4 pole. Normal,
switch to high position.
No.
Term Description
1. Three speeds change lever
2. Two speeds change lever High and low speeds change lever.
3. Indicating ring for high
and low speed.
It is to indicate the current speed.
4. Reference point for the
three speeds change lever
It refers to the current position of the three speeds
change lever.
5. Reference point for the
two speeds change lever
6. Pole change switch
Change the spindle speed as the following way:
a. Have spindle rotate.
b. Look up in the speed table and choose a suitable speed rate.
c. Turn on the switch for the feed rate.
Precaution when changing speed:
a. Spindle rotation must be stopped when at changing speed.
b. Please press down the emergent stop button for safety reason.
c. Change speed only after the spindle stops completely.
Page 53
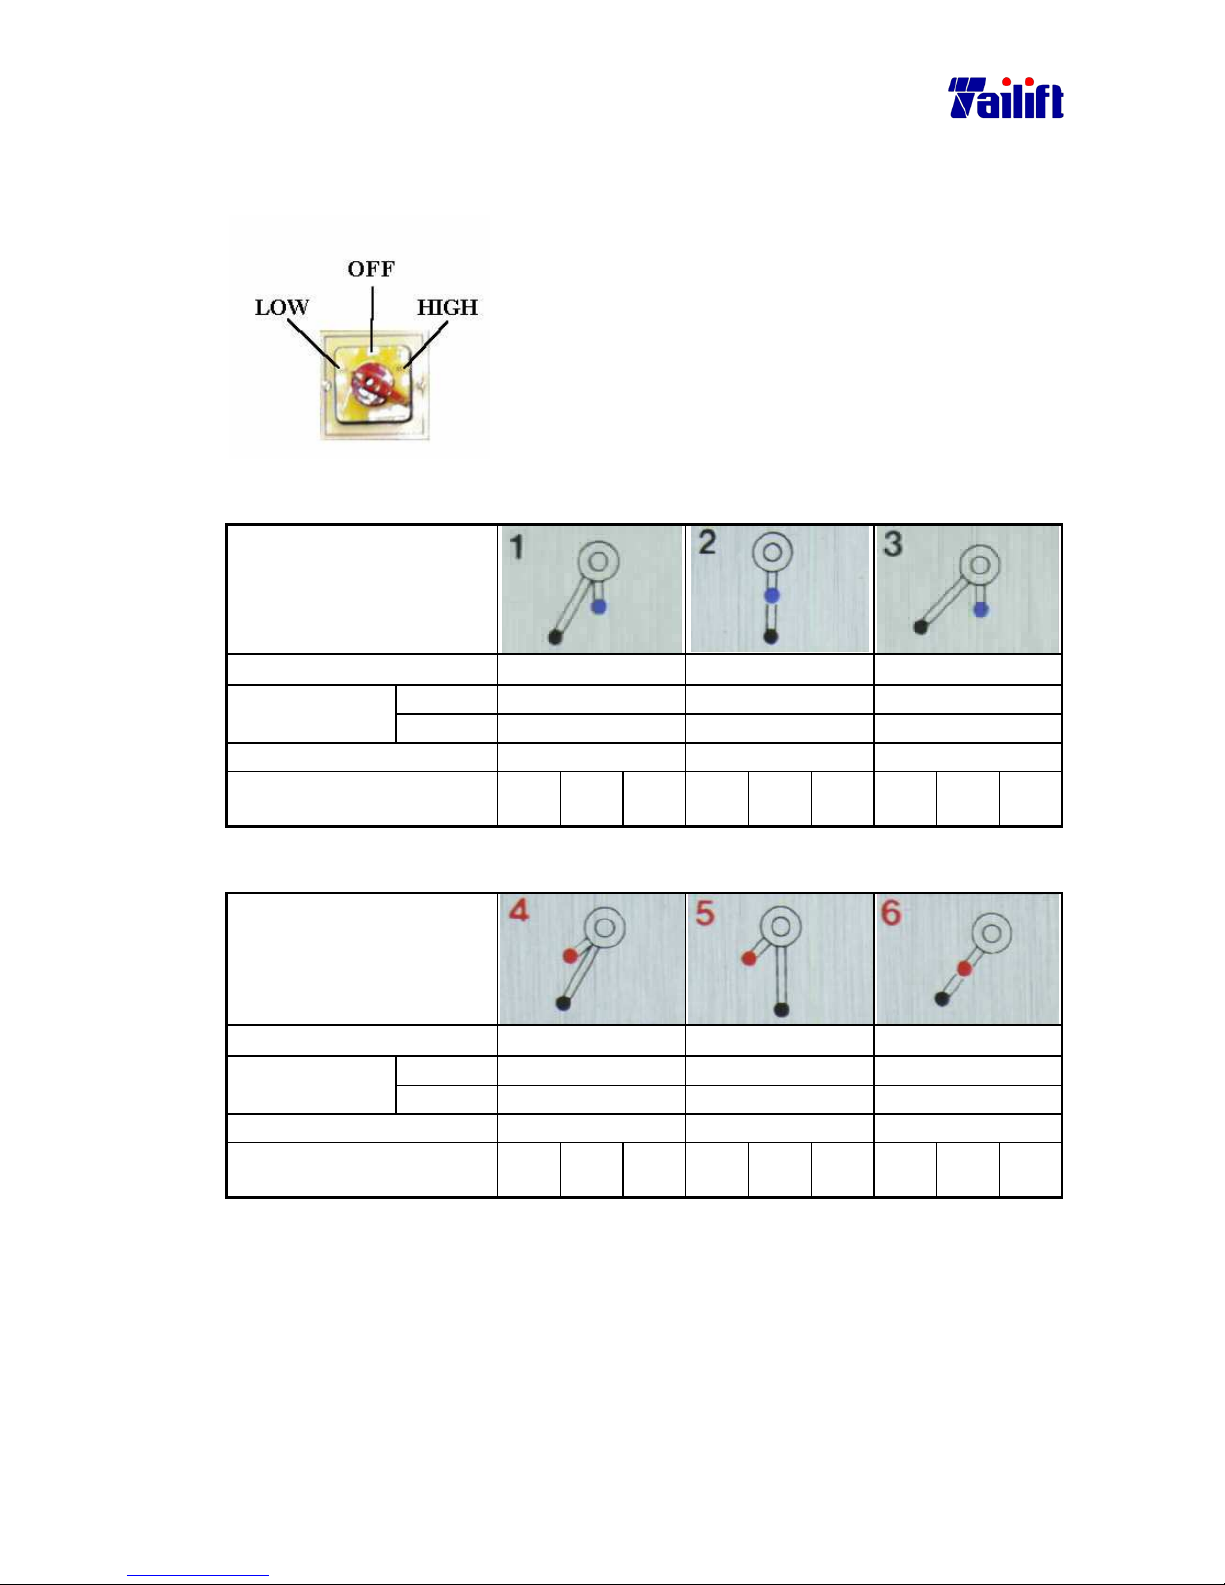
5-27
Ⅲ
ⅢⅢ
Ⅲ. The speedometer at the time
when the pole switch is in low position.
The position for the pole switch.
Two speed change lever((((low speed))))
Speed change levels
Speed((((rpm)))) 44 77 141
Mild steel
∅∅∅∅25-∅∅∅∅40 ∅∅∅∅25-∅∅∅∅40 ∅∅∅∅19-∅∅∅∅25
Suitable drilling
diameter mm
Cast iron
∅∅∅∅38-∅∅∅∅55 ∅∅∅∅38-∅∅∅∅55 ∅∅∅∅28-∅∅∅∅38
Threading (metric) M16-M20 M16-M20 M6-M16
Suitable automatic
feeding step.
1 2 3 1 2 3 1 2 3
Two speed change lever(
(
(
(high speed))))
Speed change levels
Speed((((rpm)))) 228 398 750
Mild steel
∅∅∅∅12-∅∅∅∅19 ∅∅∅∅10-∅∅∅∅12 ∅∅∅∅6-∅∅∅∅10
Suitable drilling
diameter mm
Cast iron
∅∅∅∅22-∅∅∅∅28 ∅∅∅∅19-∅∅∅∅22 ∅∅∅∅10-∅∅∅∅19
threading(metric) M3-M6 Not suggested. Not suggested.
Suitable automatic
feeding step.
1 2 3 1 2 3 1 2 3
Page 54
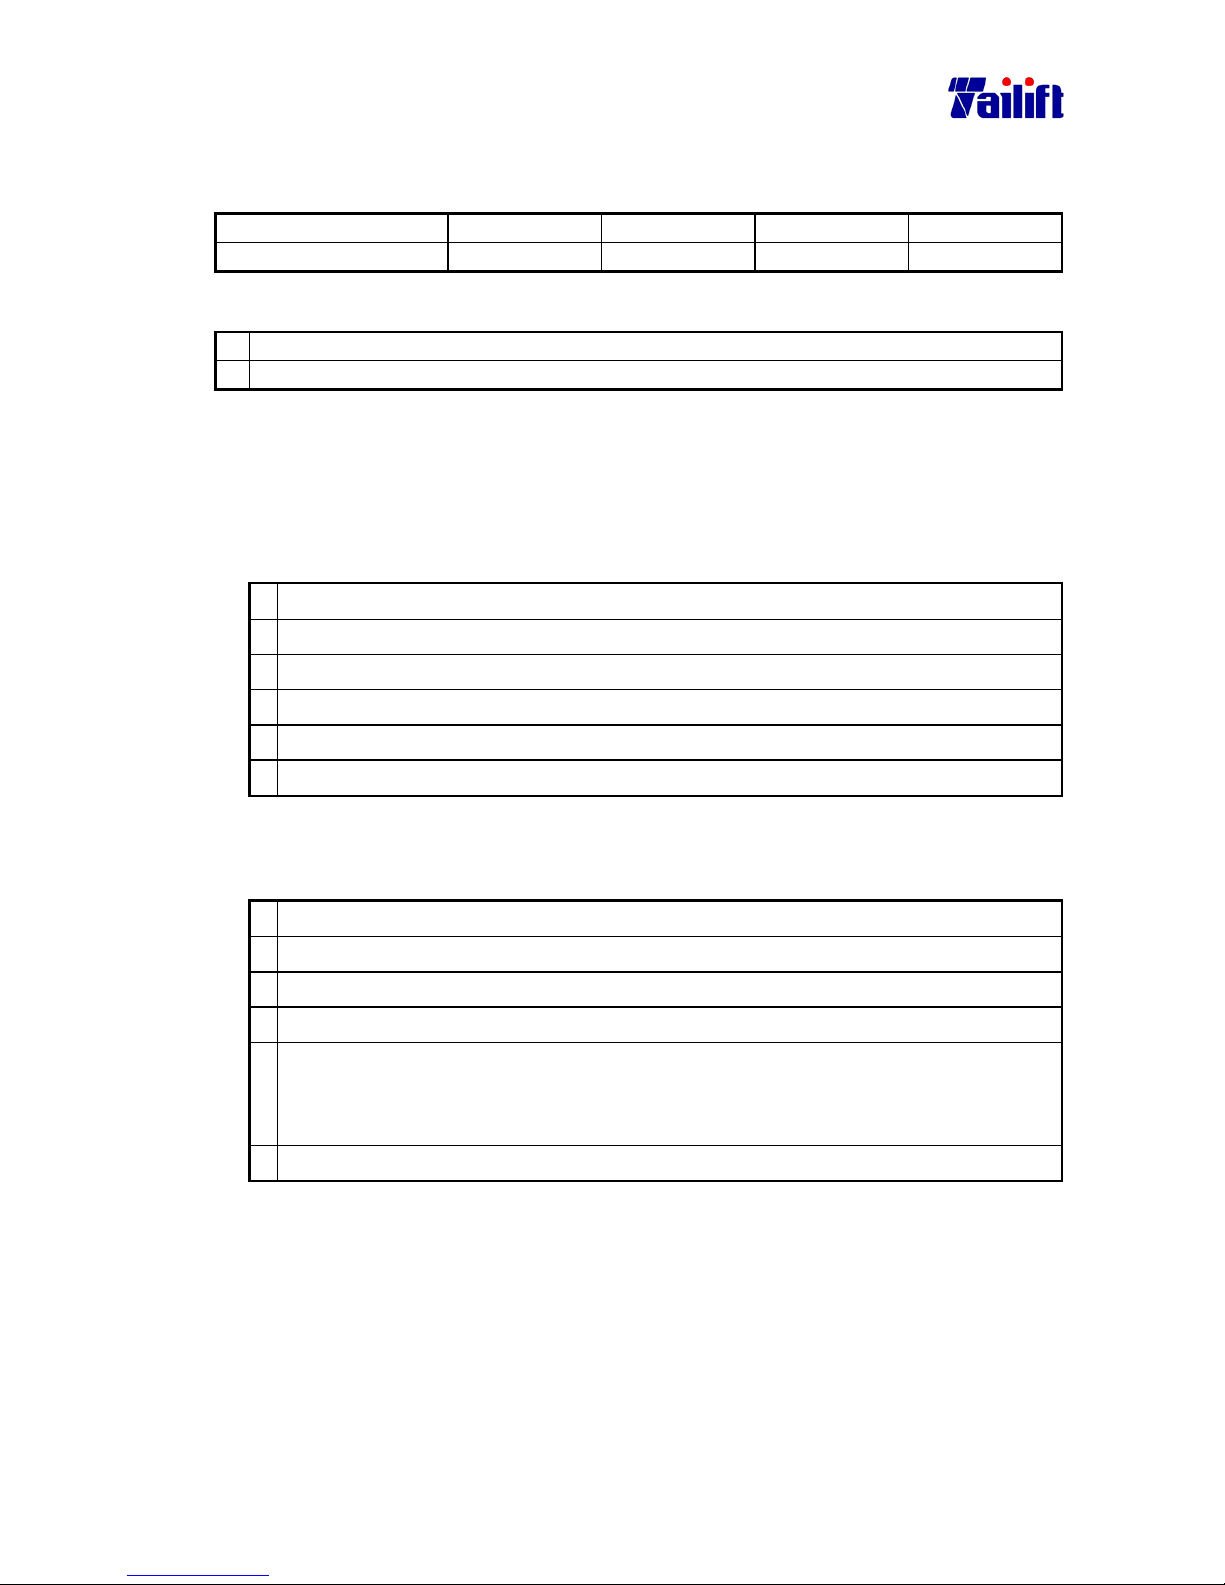
5-28
5.12 Automatic Feed
5.12.1 Automatic feed rate table
Steps N 1 2 3
Feed rate No feed rate 0.05mm/Rev 0.09 mm/Rev 0.15 mm/Rev
5.12.2 Change the feed rate as the following way:
a. Check the speedometer and choose a suitable rate.
b. Switch the feed rate.
Precaution when at changing feed rate:
You can change the feed rate only when the spindle is rotating.
5.12.3 Suppose that the work piece is by the machine
The way to move((((less than 25 kgs.))))
Suppose that the work piece is by the machine, the way to move it is as follows:
1. Power off.
2. Put on gloves.
3. Squat facing the work piece.
4. Lift the work piece with two hands.
5. When you are standing up, lift and move the work piece with your feet strength.
6. Move the work piece toward the worktable.
The way to move((((greater than 25 kgs.))))
Suppose that the work piece is by the machine, the way to move it is as follows:
1.
Power off.
2. Put on gloves.
3. Push the arm backwards.
4. Move a lifting devise close to the work piece.
5. Place lifting ropes or slings under the work piece, (please use two ropes or
slings). If the work piece has holes for lifting ropes or slings, please lock it with
ring head pin, then lift and move it with a hook.
6. Move the work piece toward the worktable.
Page 55
5-29
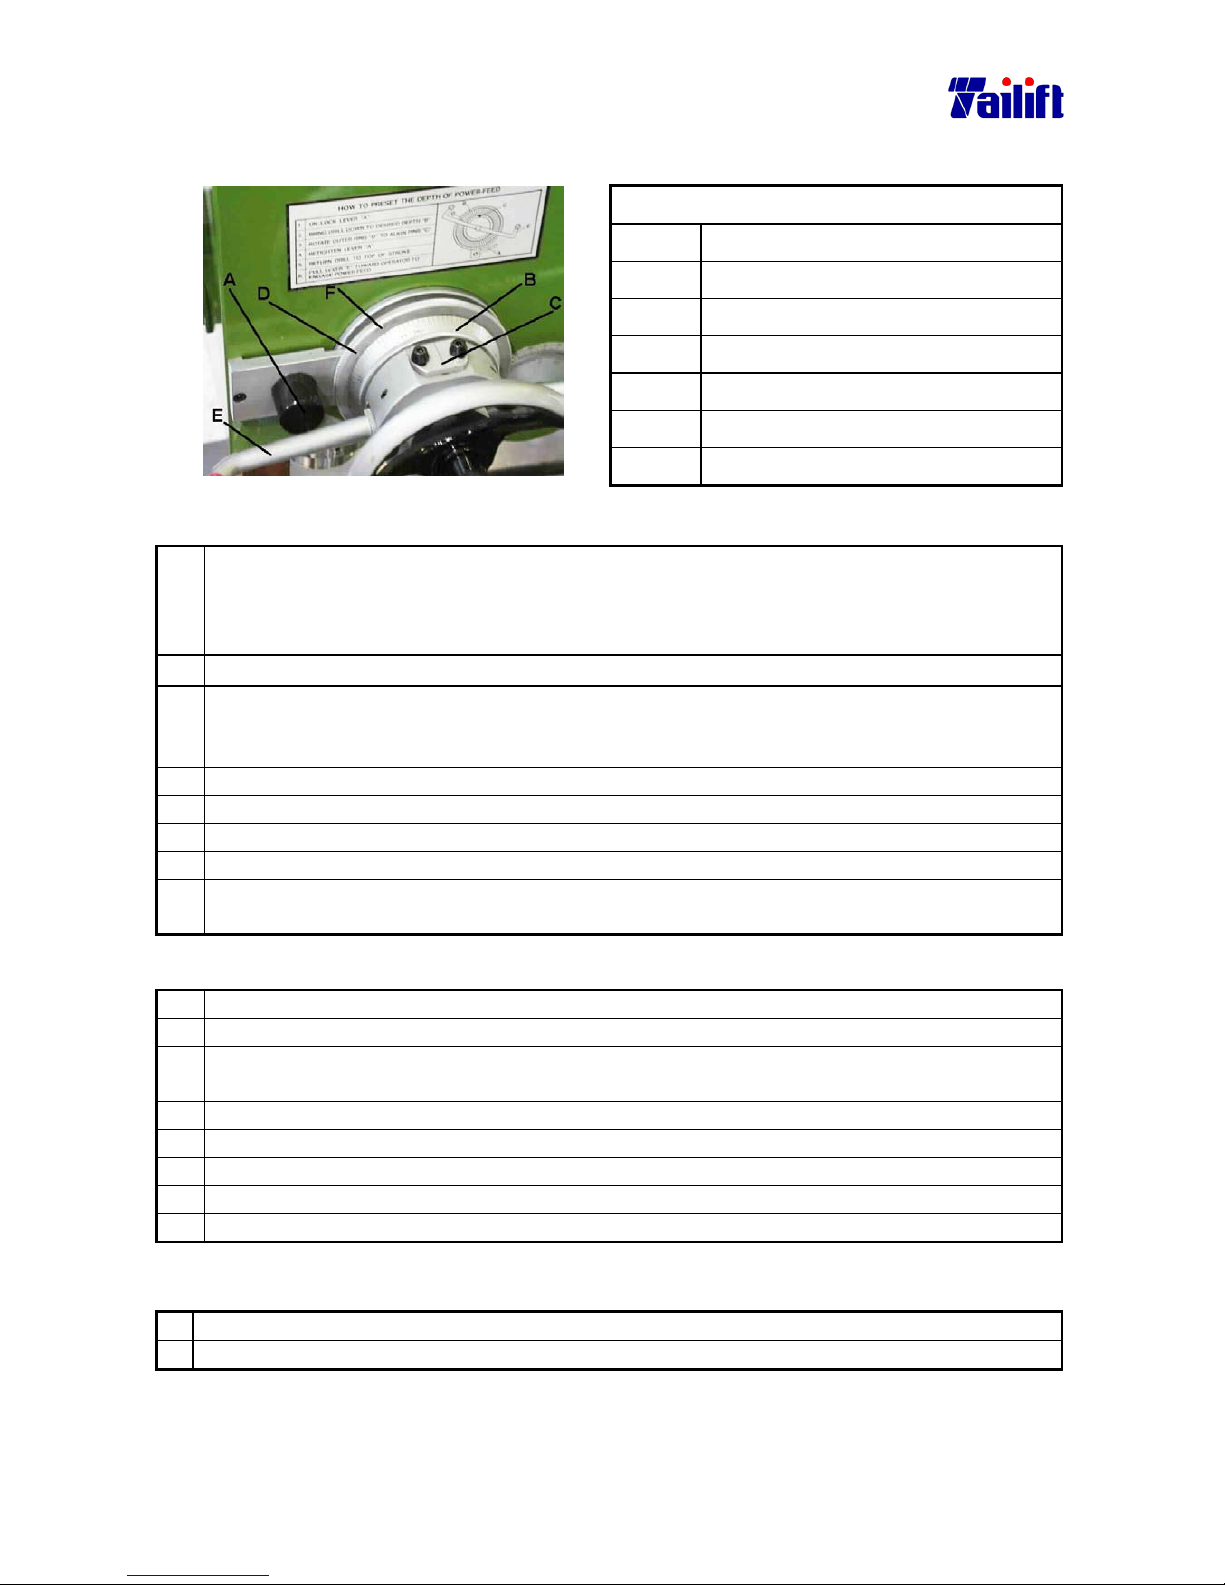
5.12.4 How to preset the depth of the power-feed?
Ⅰ
ⅠⅠ
Ⅰ.(For TPR-720A, TPR-820A, TPR-920A)
The relevant terms
NO.
Term
A
Depth controlling and fixing lever.
B
Main dial
C
Clutch adjusting block
D
Depth-setting ring
E
Feed trip lever
F Depth reference point.
Preset the depth of the power-feed:
a. Rotate the feed trip lever counter clockwise as shown in picture E till The drill bit
contact the work piece. (At this moment, B and C shown in the pictures move
simultaneously. That’s the depth is zero when the bit is contacting the work piece and
the dial is also at the zero position. )
b. Release the fixing lever of the main dial. That’s to release A shown in the picture.
c. Rotate the depth setting ring as shown in picture D, referring to the depth point on the
ring. To set the drilling depth is to adjust and align the gauge on the ring as shown in
the picture B.
d. Clamp the fixing lever of the main dial. That’s to clamp A shown in the picture.
e. Release the feed trip lever as shown in the picture E.
f. Rotate the feed trip lever a little bit counter clockwise, as shown in the picture E.
g. Turn the spindle switch to “SPDL. FOR”.
h. Pull the feed trip lever backwards as shown in the picture E, The spindle will feed at the
chosen rate and stop
Example::::How to preset a depth of 30mm?
a. Rotate E as in the picture till it contacts the work piece.
b. Release A, as shown in the picture.
c.
Rotate D and align F as shown in the picture to the position of 30 mm on the B, as shown
in the picture.
d. Clamp A, as shown in the picture.
e. Release E, as shown in the picture.
f. Rotate E in the picture a little bit counter clockwise.
g. Turn the spindle switch to SPDL. FOR
h. Pull the feed trip lever as shown in the picture E backwards.
Precaution
a. Auto feed will move only after the feed rate is set up.
b. Auto feed is used only in drilling, not in threading.
Page 56
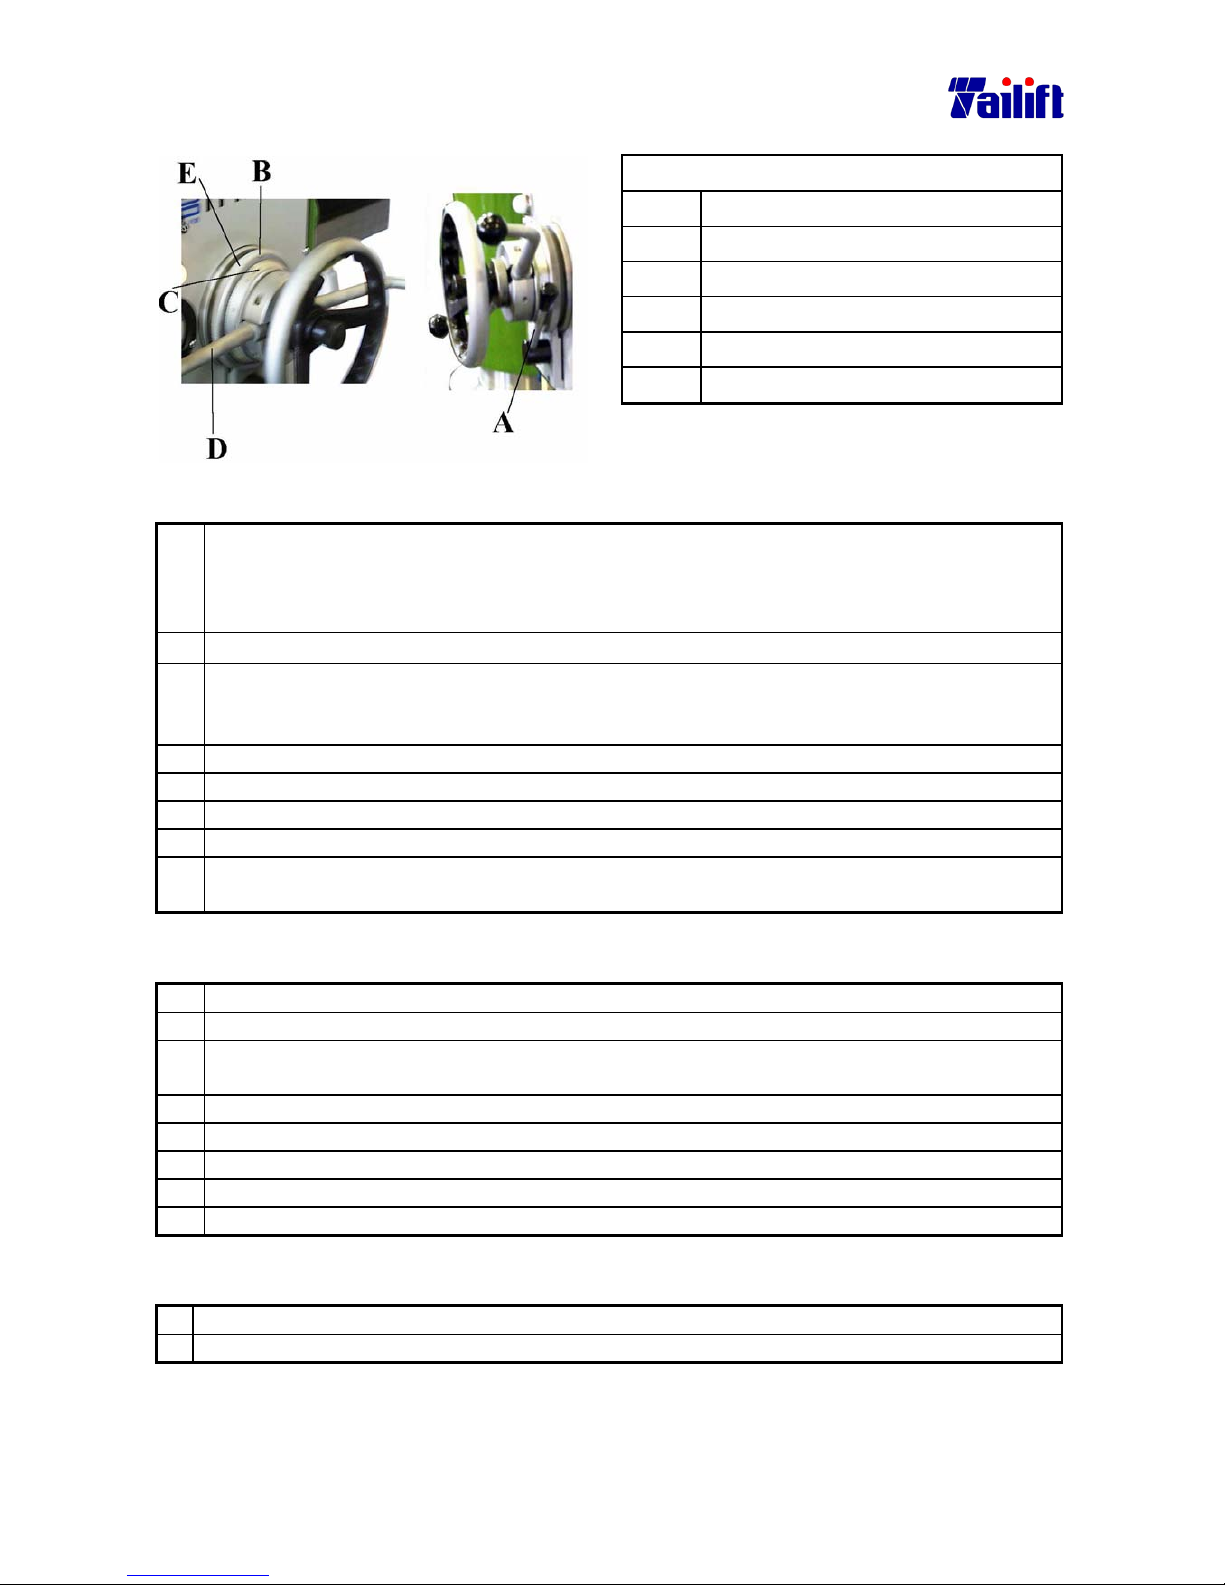
5-30
Ⅱ
ⅡⅡ
Ⅱ.(For TPR-1100)
The relevant terms
NO. Term
A Depth controlling and fixing lever.
B Depth reference point.
C Main dial
D Feed trip lever
E Depth-setting ring
Preset the depth of the power-feed:
a. Rotate the feed trip lever counter clockwise as shown in label D till The drill bit contact
the work piece. (At this moment, label B shown in the pictures move simultaneously.
That’s the depth is zero when the bit is contacting the work piece and the dial is also at
the zero position. )
b. Release the fixing lever of the main dial. That’s to release label A shown in the picture.
c. Rotate the depth setting ring as shown in label E, referring to the depth point on the
ring label B. To set the drilling depth is to adjust and align the gauge on the ring as
shown in the label C.
d. Clamp the fixing lever of the main dial. That’s to clamp label A shown in the picture.
e. Release the feed trip lever as shown in the label D.
f. Rotate the feed trip lever a little bit counter clockwise, as shown in the label D.
g. Turn the spindle switch to “SPDL. FOR”.
h. Pull the feed trip lever backwards as shown in the label D, The spindle will feed at the
chosen rate and stop
Example::::How to preset a depth of 30mm?
a. Rotate D as in the picture till it contacts the work piece.
b. Release A, as shown in the picture.
c. Rotate E and align C as shown in the picture to the position of 30 mm on the B, as
shown in the picture.
d. Clamp A, as shown in the picture.
e. Release D, as shown in the picture.
f. Rotate D in the picture a little bit counter clockwise.
g. Turn the spindle switch to SPDL. FOR
h. Pull the feed trip lever as shown in the picture D backwards.
Precaution
a. Auto feed will move only after the feed rate is set up.
b. Auto feed is used only in drilling, not in threading.
Page 57
5-31
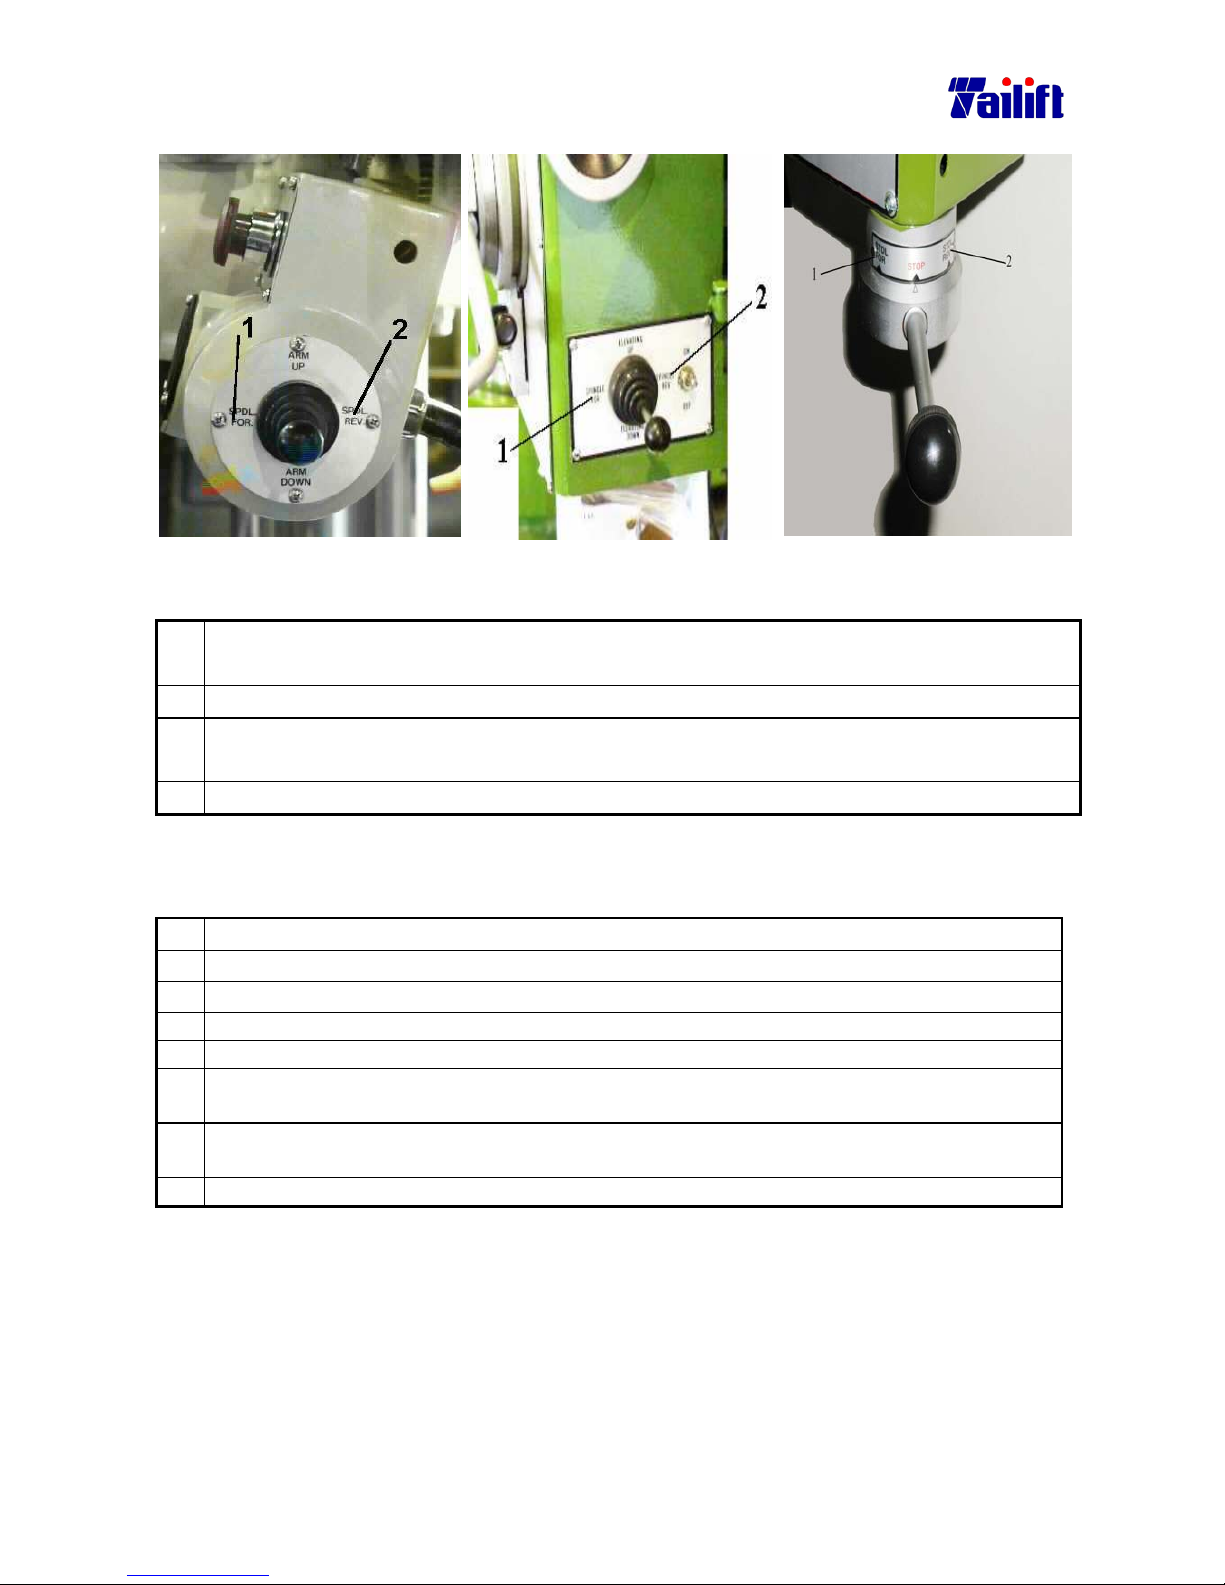
5.13 The spindle
(For TPR-720A, TPR-820A,
TPR-920A)
(For TPR-1100)
(Type I)
(ForTPR720A,TPR820A,
TPR920A, TPR-1100)
(Type II)
1.
Please turn on the main switch of the machine , and then lower down the
Quill by 5 mm , so that the forward/reverse of the main spindle can start.
2.
The main spindle will forword when switching to SPDL.FOR.
3.
If you want to stop the rotating of the spindle, please switch to the middle
Position.
4.
The main spindle will reverse when switching to SPDL.FOR.
5.14 Threading
The way to thread is as follows::::
a. Clamp the screw tap with drilling head.
b. Move the spindle to the top of the threading.
c. Set the feed rate at ”N”。。。。
d. Rotate the feed trip lever a little bit counter clockwise.
e. After the cross switch turned to “SPDL.FOR”, the spindle spins clockwise.
f. Rotate the feed trip lever counter clockwise till the threading is finished. (The operator
decides the threading depth.)
g.
After the cross switch turned to “SPDL.REV.”, let the spindle turn counter clockwise till
the screw tap retreats completely.
h. Turn the cross switch to the middle to stop the spindle.
Page 58
5-32
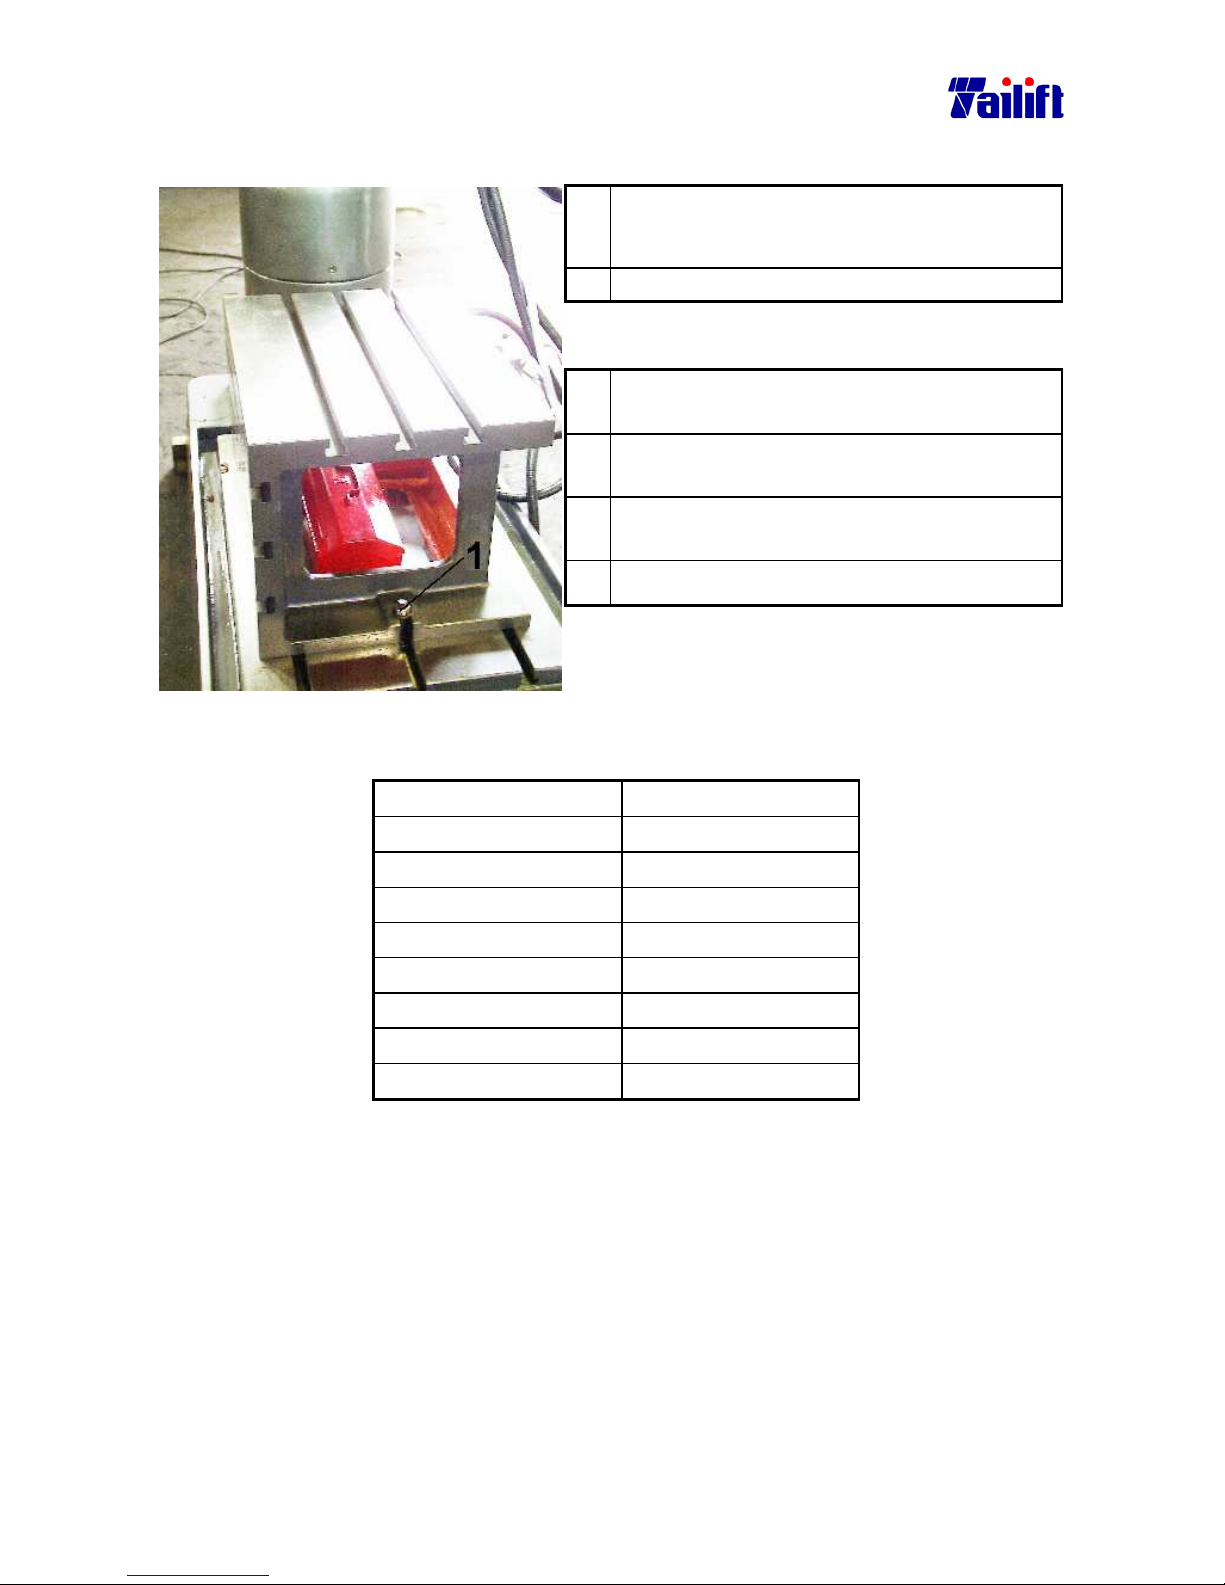
5.15 The assembly and disassembly of the work table.
Disassemble it as follows:
1. Release 1, as shown in the picture, using a
spanner. That’s to move the spanner counter
clockwise.
2. Apply the above to the other side.
Assembly it as follows:
1. Clean the debris from the base with a
metal brush.
2. Clean the worktable and the base with
rags.
3. Place T shape Bolts into the T shape
chamfer of the base.
4. Tighten the nuts.
5.16 Cutting fluids for all kinds of material.
Soft steel
crude oil、、、、animal fat
Mild steel
crude oil、、、、animal fat
High carbon steel
crude oil、、、、animal fat
Stainless steel
crude oil、、、、animal fat
Manganese steel
crude oil、、、、animal fat
Cast iron Without
Malleable cast iron Crude oil
Brass, bronze Kerosene
Aluminum and alloy Kerosene
Precaution
When cutting fluids is not applied, Having the turning speed and the feed rate
reduced is the only way to extend the tool life. If cutting fluids leaks or injects
to the aisle, please clean it immediately from the floor.
Page 59
6-1
CHAPTER 6
Adjustment
6.1General
Adjustment is needed after the machine has been used a period of time for its parts
will get loose or worn out, In the radial drill, there are three parts needed to be adjusted.
One is the arm clamping lever, another the gap between the gearbox and the arm rail,
finally the engagement between the feed trip lever and the clutch and
Maximum Range
for spindle adjustment.
6.2 The arm clamping lever
After the machine has been used for about 3-5 years, the position of the arm clamping
lever will be descending. It is the time to adjust the position of the arm clamping lever.
Pic. a. Pic. b.
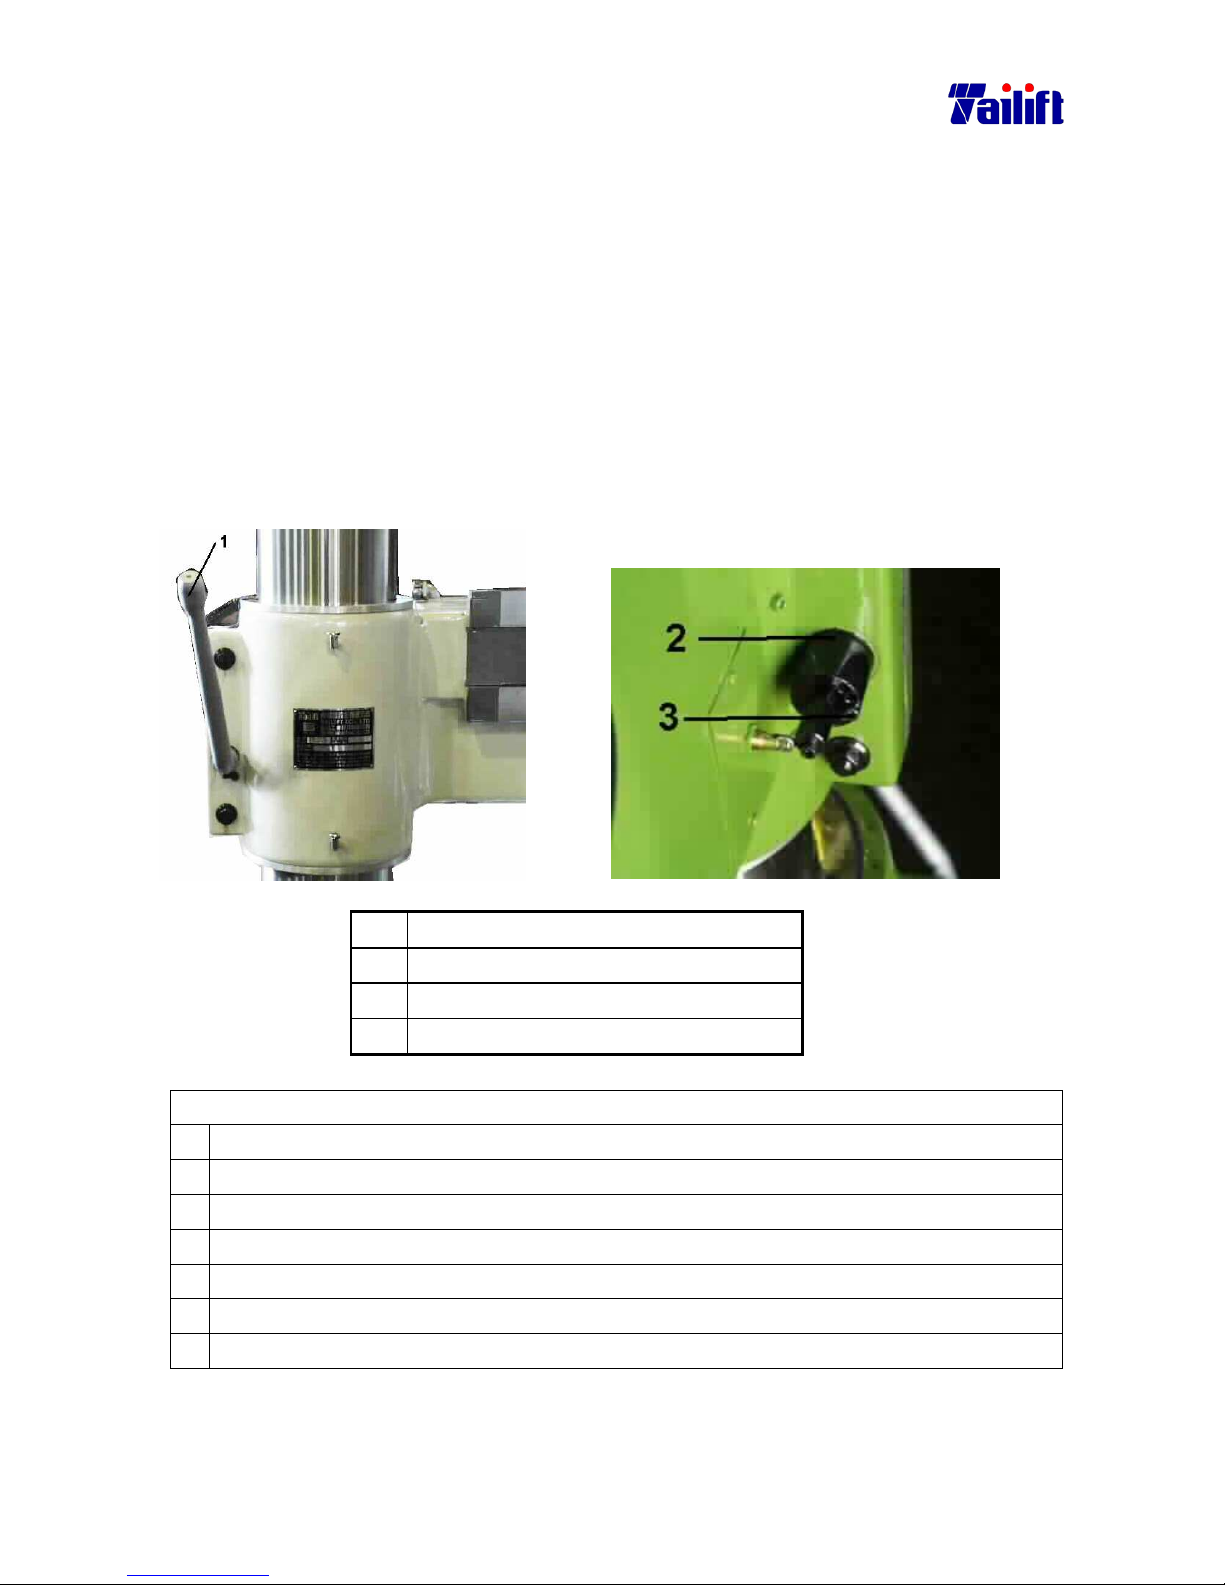
No.
Term
1. The arm clamping lever
2. The nuts for adjusting the lever.
3. Fixing bolts
Adjust the arm clamping lever as follows:
a. Power off.
b. Press down the emergent stop button.
c. Release the arm clamping lever.( as no. 1 in the pic. a)
d.
Release the fixing bolts((((as No. 3 in the pic. b.))))
e. Rotate the arm adjusting nuts one turn clockwise. ( as No. 2 in pic. b.)
f.
Tighten the fixing bolts((((as No. 3 in the pic. b.))))
g.
Tighten the arm clamping lever.((((as No. 1 in the pic. a.))))
Page 60
6-2
6.3 The gap adjustment between the gearbox and the arm rail
After the machine has been used a period of time, the gap between the gearbox and the arm
rail appears. It is the time to adjust its tightness between the arm rail and crank shaft bearing.
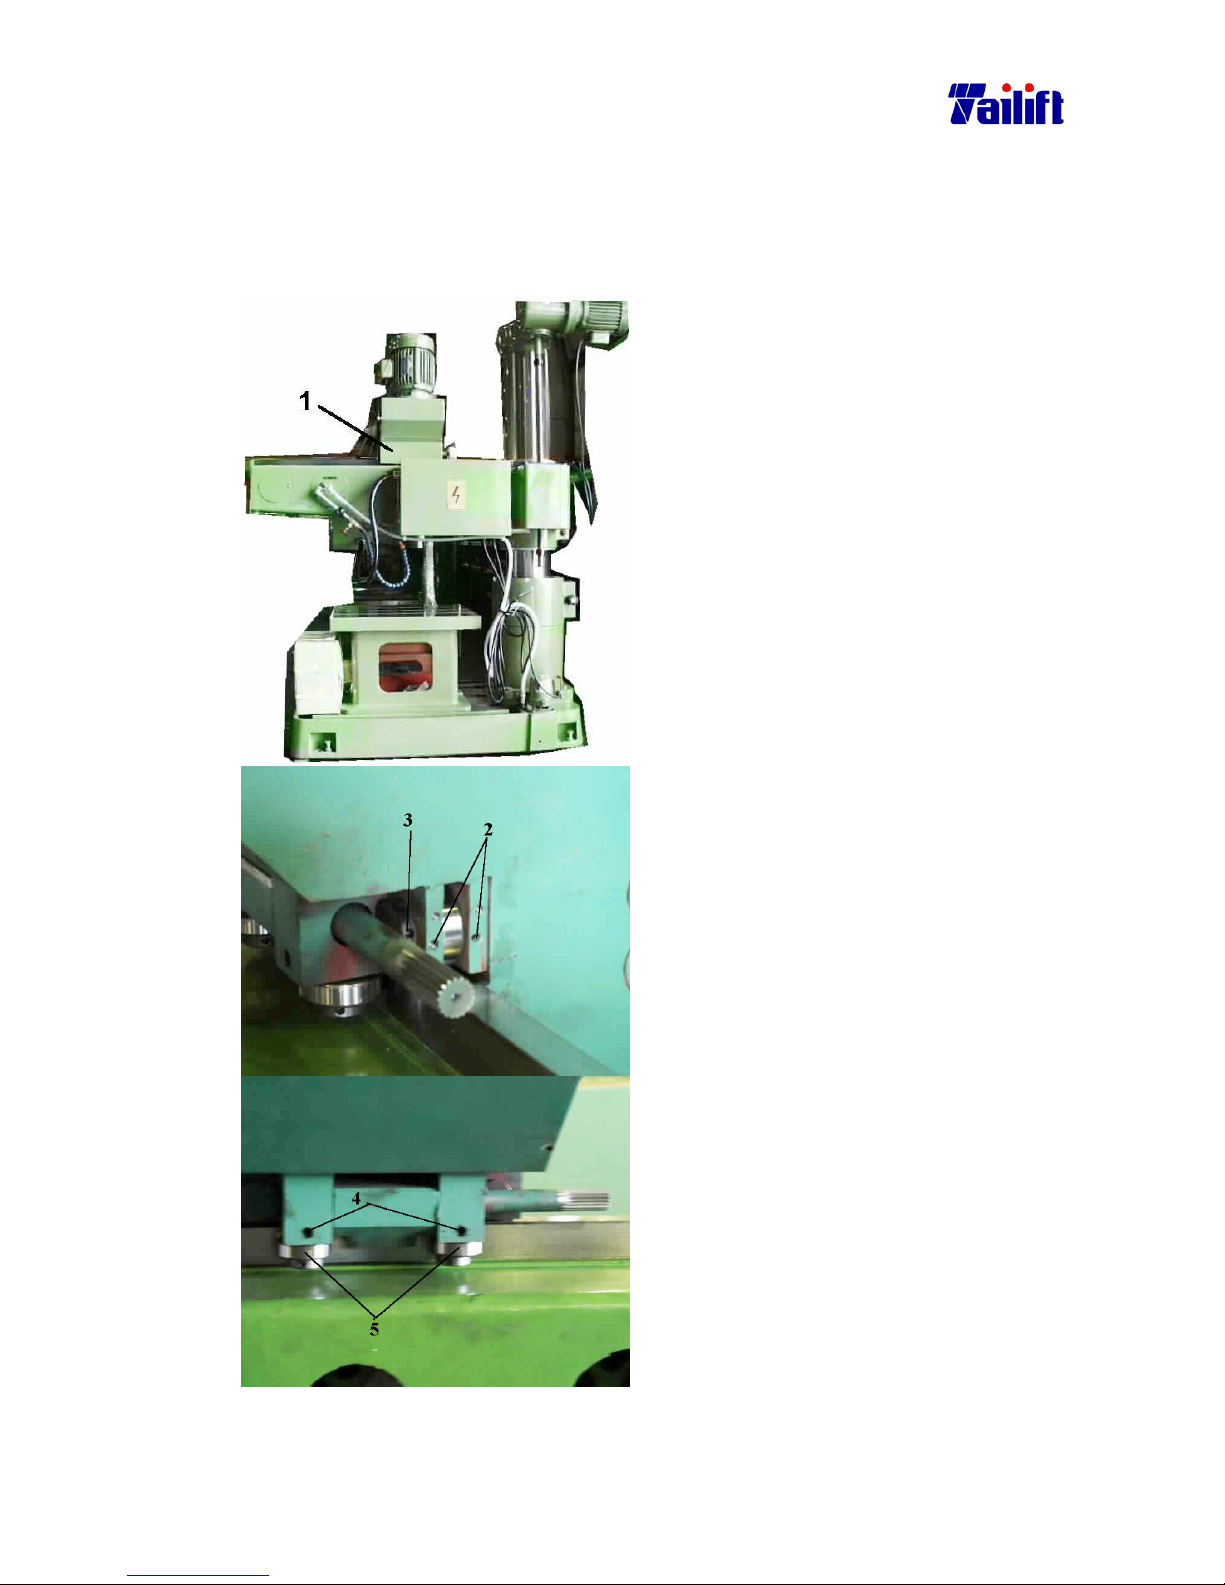
6.3.1 (For TPR-720A, TPR-820A, TPR920A)
a. Dismantle the metal cover, as shown
in the picture 1.
Release the bolts as shown in the
picture 2.
b.
Using a hex wrench, insert it into the
hole as shown in the pic. 3 and rotate
it till that you can easily turn the
hand wheel of the gearbox
but can’t
move it without any force. Apply the
same to the opposite site.
Release the bolts as shown in the
picture 4.
c.
Using a hex wrench, insert it into the
hole as shown in the pic. 3 and rotate
it till that you can easily turn the
hand wheel
of the gearbox but can’t
move it without any force. Apply the
same to the opposite site.
Page 61
6-3
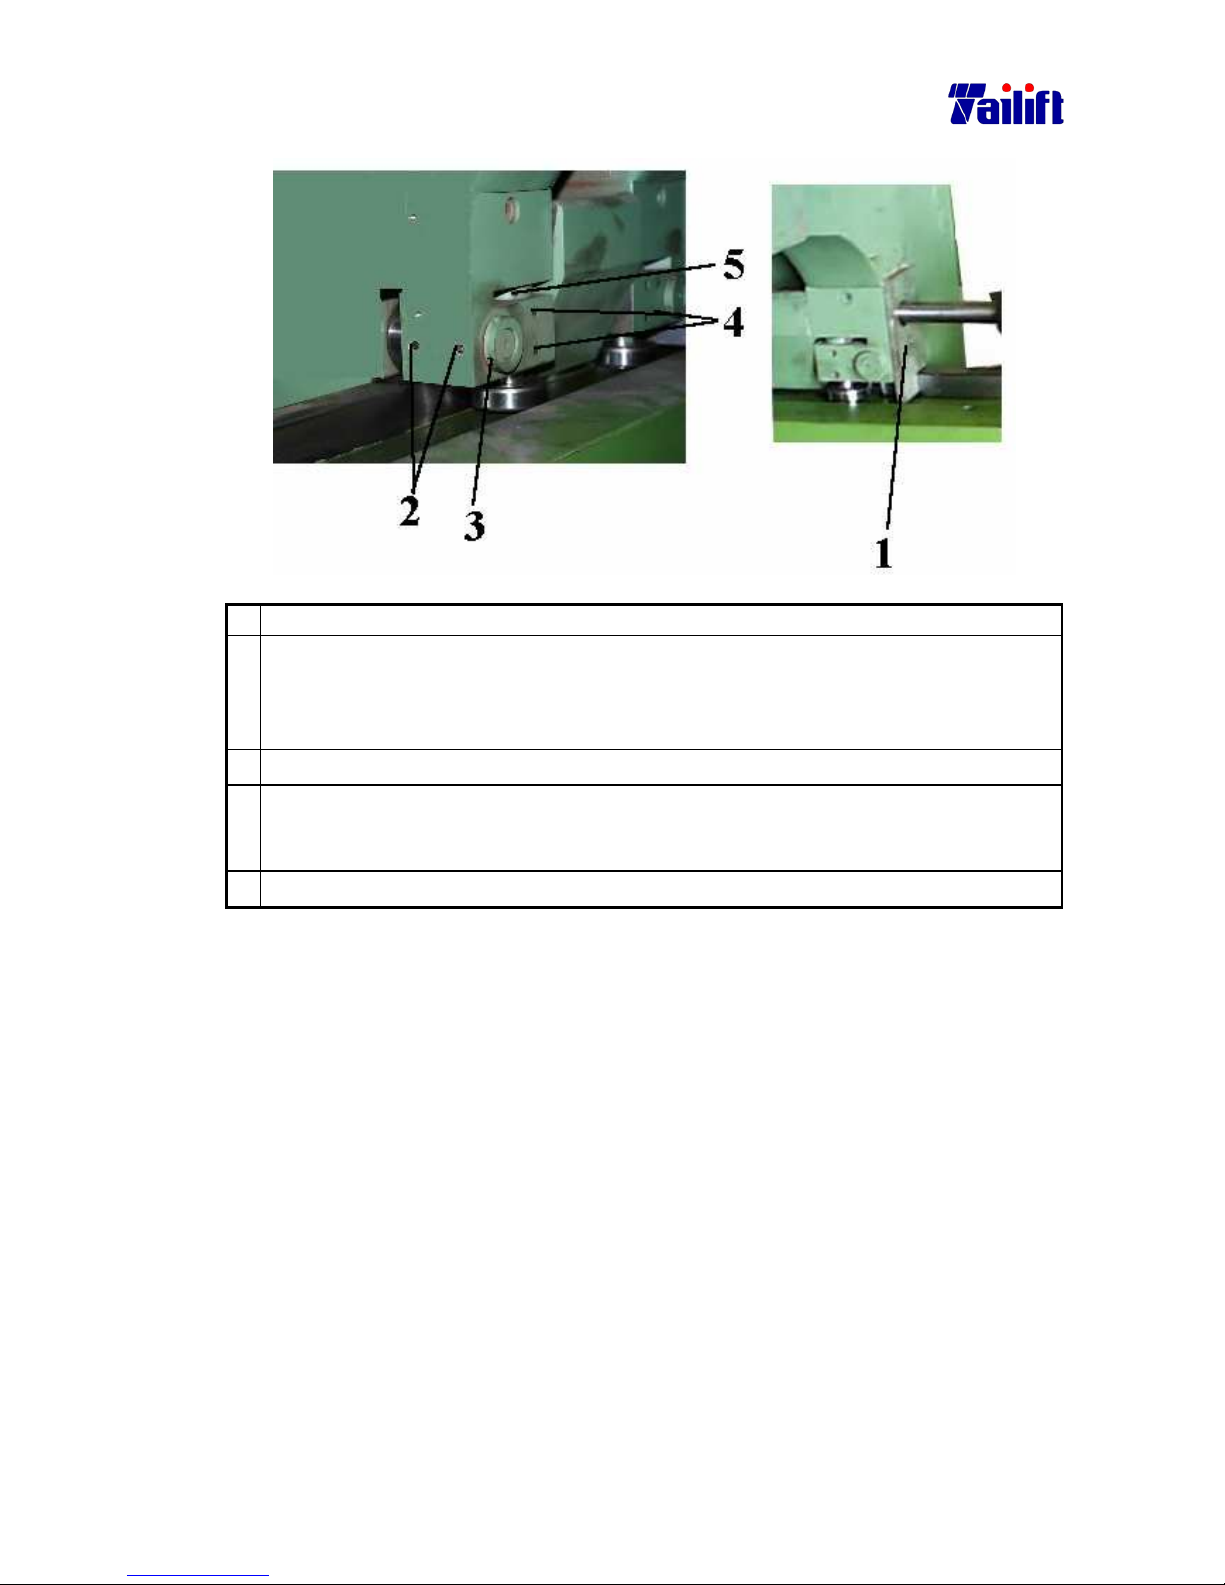
6.3.2 (For TPR-1100)
a. Remove the side plate as the above figure 1.
b. Release the bolts as the above figure 2. Using socket wrench
, insert it into the holes
as shown in the above figure 3 and rotate them. Apply the tightness as the hand
wheel of the Gearbox can be turned easily but not too easily. Apply the same to the
counter side.
c.
Release the bolts as shown in the right figure 4.
d.
Using socket wrench, insert it into the holes as shown in the above figure 5 and
rotate them. Apply the tightness as the hand wheel of the Gearbox can be turned
easily but not too easily. Apply the same to the counter side.
e. Screw up the side plate of the above figure 1.
Page 62
6-4
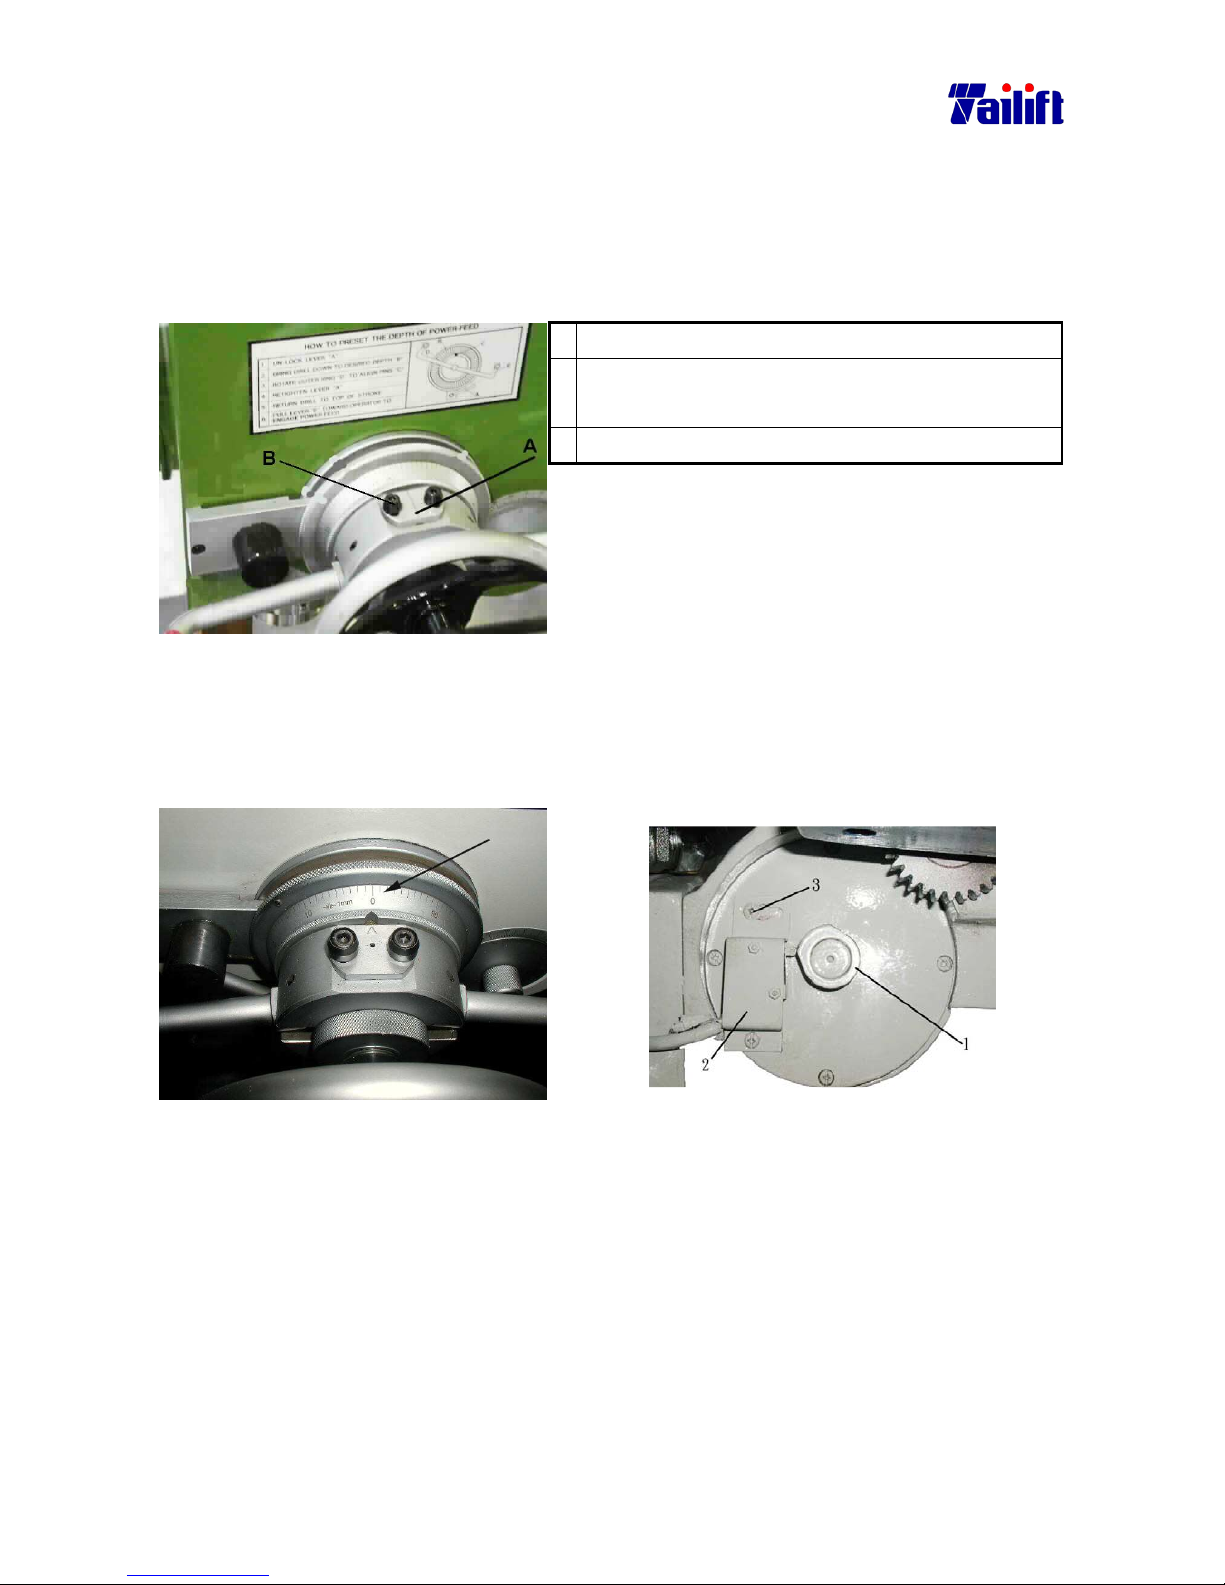
6.4 Adjust the engagement between the feed trip lever and the clutch
After the machine has been used a period of time, gap between the feed trip lever
and the clutch will appears. It is then the time to adjust the engagement between the feed
trip lever and the clutch.
a. Release the bolts B as shown in the right picture.
b. Push the adjusting block forwards, using a hex
wrench, as shown in the right picture.
c. Tighten the bolts B as shown in the right picture.
6.5 Maximum Range for spindle adjustment
Maximum Range for spindle adjustment Maximum Range for spindle adjustment
Maximum Range for spindle adjustment
(For TPR-720A, TPR-820A, TPR-920A)
When you find the spindle adjustment range for maximum and minimum are different or you
change the spring seat, please readjust the clearance for the spindle 3 to 5 mm to prevent
the spare part get damage.
a. In the left photo you will see the spindle gradua
tion.
b. First rotate the spindle to the upper maximum position. Let it has 3 to 5mm clearance.
See the right photo. Rotate the CAM 1 to touch the limit switch 2.
Second rotate the spindle to the lower minimum position. Let it has 3 to 5mm clearance.
Tighten the CAM fix screw and screw 3.
c. Rotate the CAM to touch the limit switch slowly. When you hear the crack noise, you can tighten
the screw.
Page 63
7-1
CHAPTER 7
Maintenance
7.1 General
Whether the machine is maintained well or not will lead to its long or short life. If well
served, the machine lasts long and is easy to maintain.
7.2 Daily Maintenance.
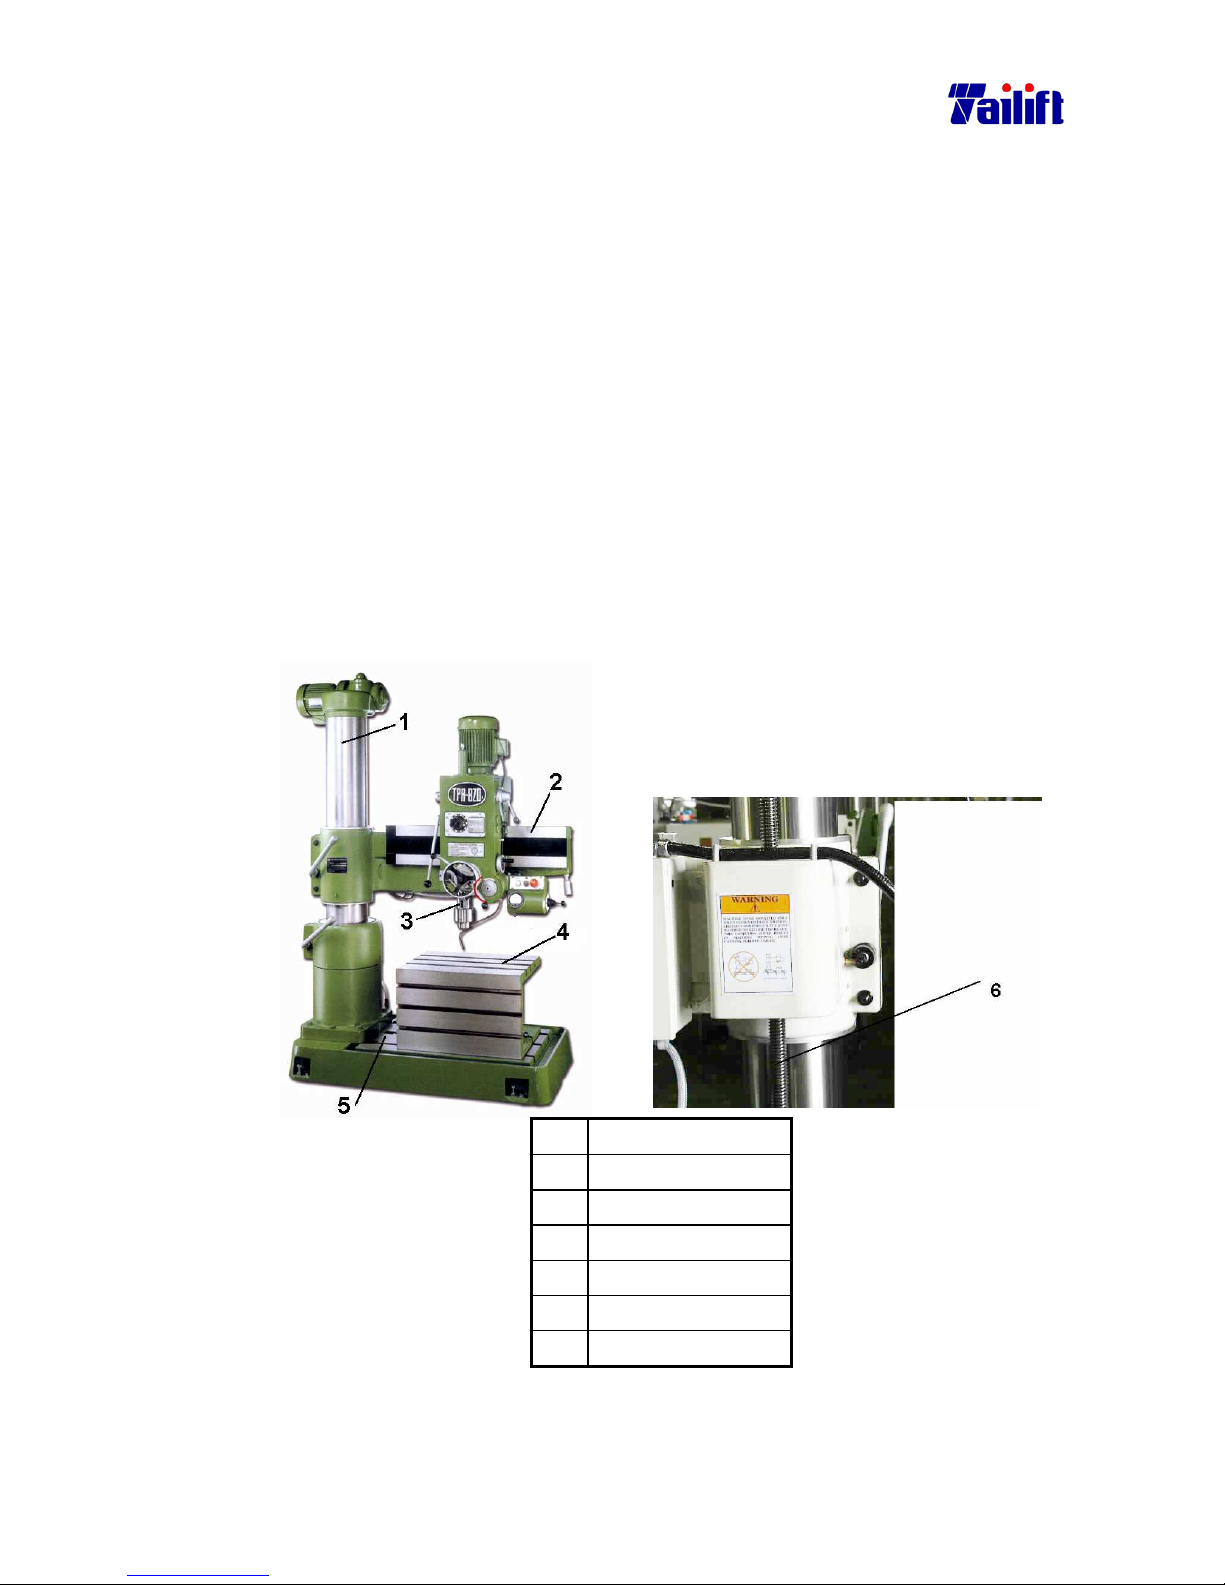
7.2.1 Clearing
Only one person is allowed to do the clearing. Before clearing, please power off.
7.2.2 Please clean every parts using a metal
brush and a rag, dipped with oil, to rub them.
(
((
(Please use CC68 ))))After every day’s work, please proceed the following
maintenance.
Ⅰ
ⅠⅠ
Ⅰ. (For TPR-720A, TPR-820A, TPR-920A)
No. Parts
1. Column
2. The arm rail
3. Spindle
4. Work table
5. The base
6. The ball screw
Page 64
7-2
Ⅱ
ⅡⅡ
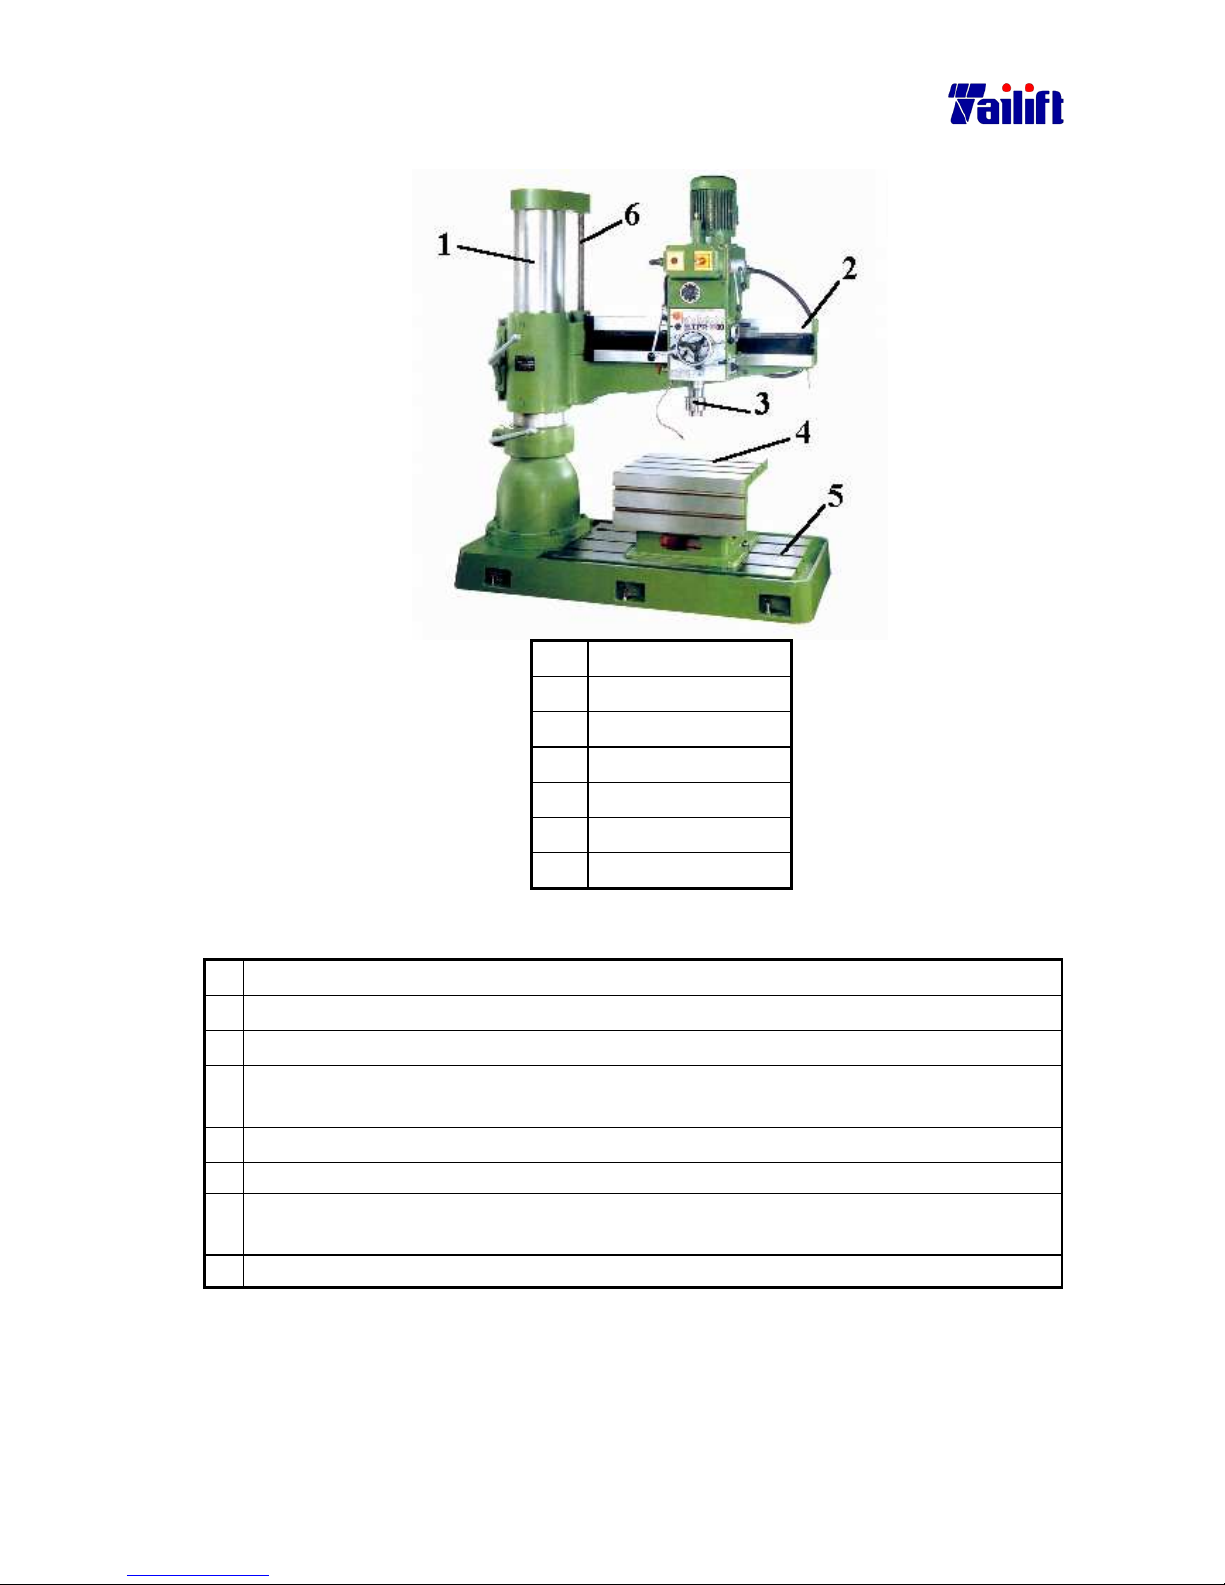
Ⅱ. (For TPR-1100)
No. Parts
1. Column
2. The arm rail
3. Spindle
4. Work table
5. The base
6. The ball screw
7.2.3 The way to clean iron filings:
1.
Power off.
2.
Put on gloves.
3.
Clean from upside down using a brush.
4.
When the iron filings comes down to the base, please collect it and put it at the right
side of the operation position.
5.
Find a dustpan and place it under the machine.
6. Sweep it to the dustpan using the brush.
7. Rub every part of the machine with rags, particularly the parts where is
contaminated with the cutting fluids.
8. Rub every metal part of the machine using a oil-dipped rags.
Page 65
7-3
7.2.4 Lubrication
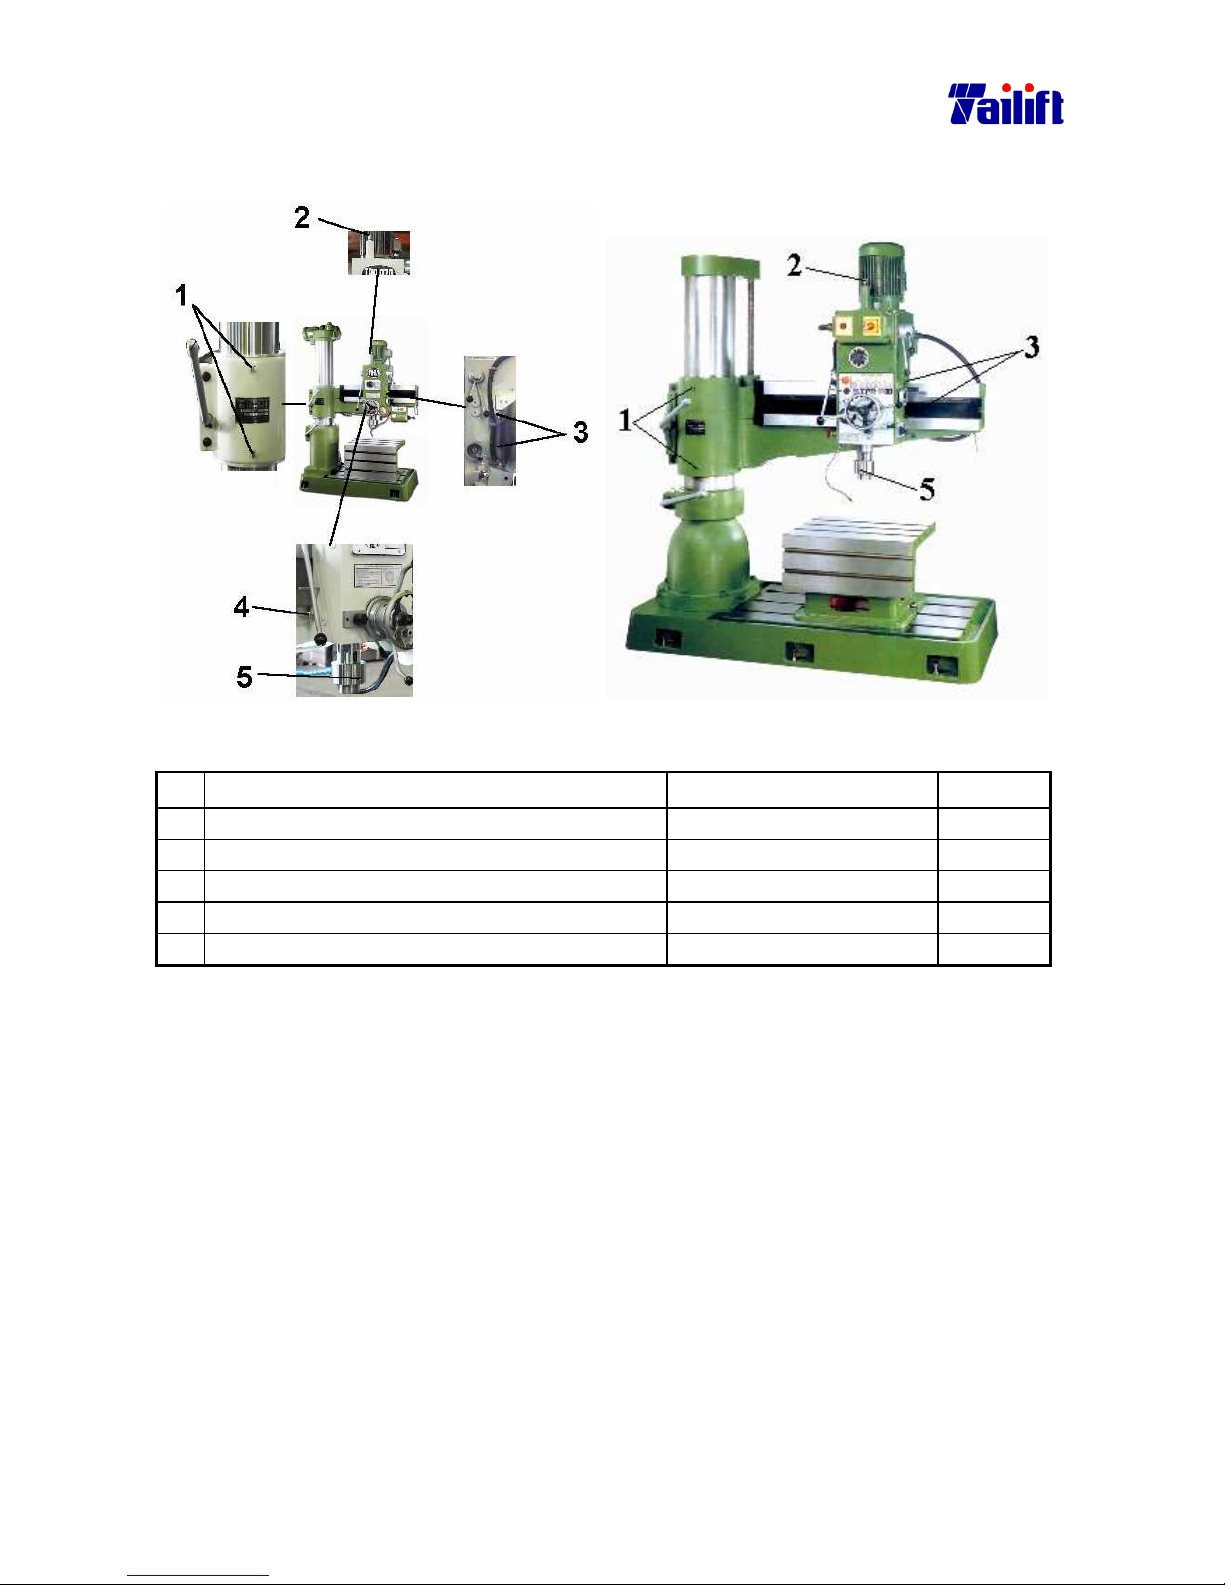
Before every day’s work, please proceed the following maintenance.
(For TPR-720A, TPR-820A, TPR-920A) (For TPR-1100)
No.
Part Oil type Volume
1. Oil filler points of the column CC68 Full
2. Oil filler points on top of the gearbox. CC68 Full
3. Oil filler points in the right side of the gearbox.
CC68 Full
4. Oil filler points in the left side of the gearbox. CC68 Full
5. Oil filler points of the spindle. XM2 Full
Page 66
7-4
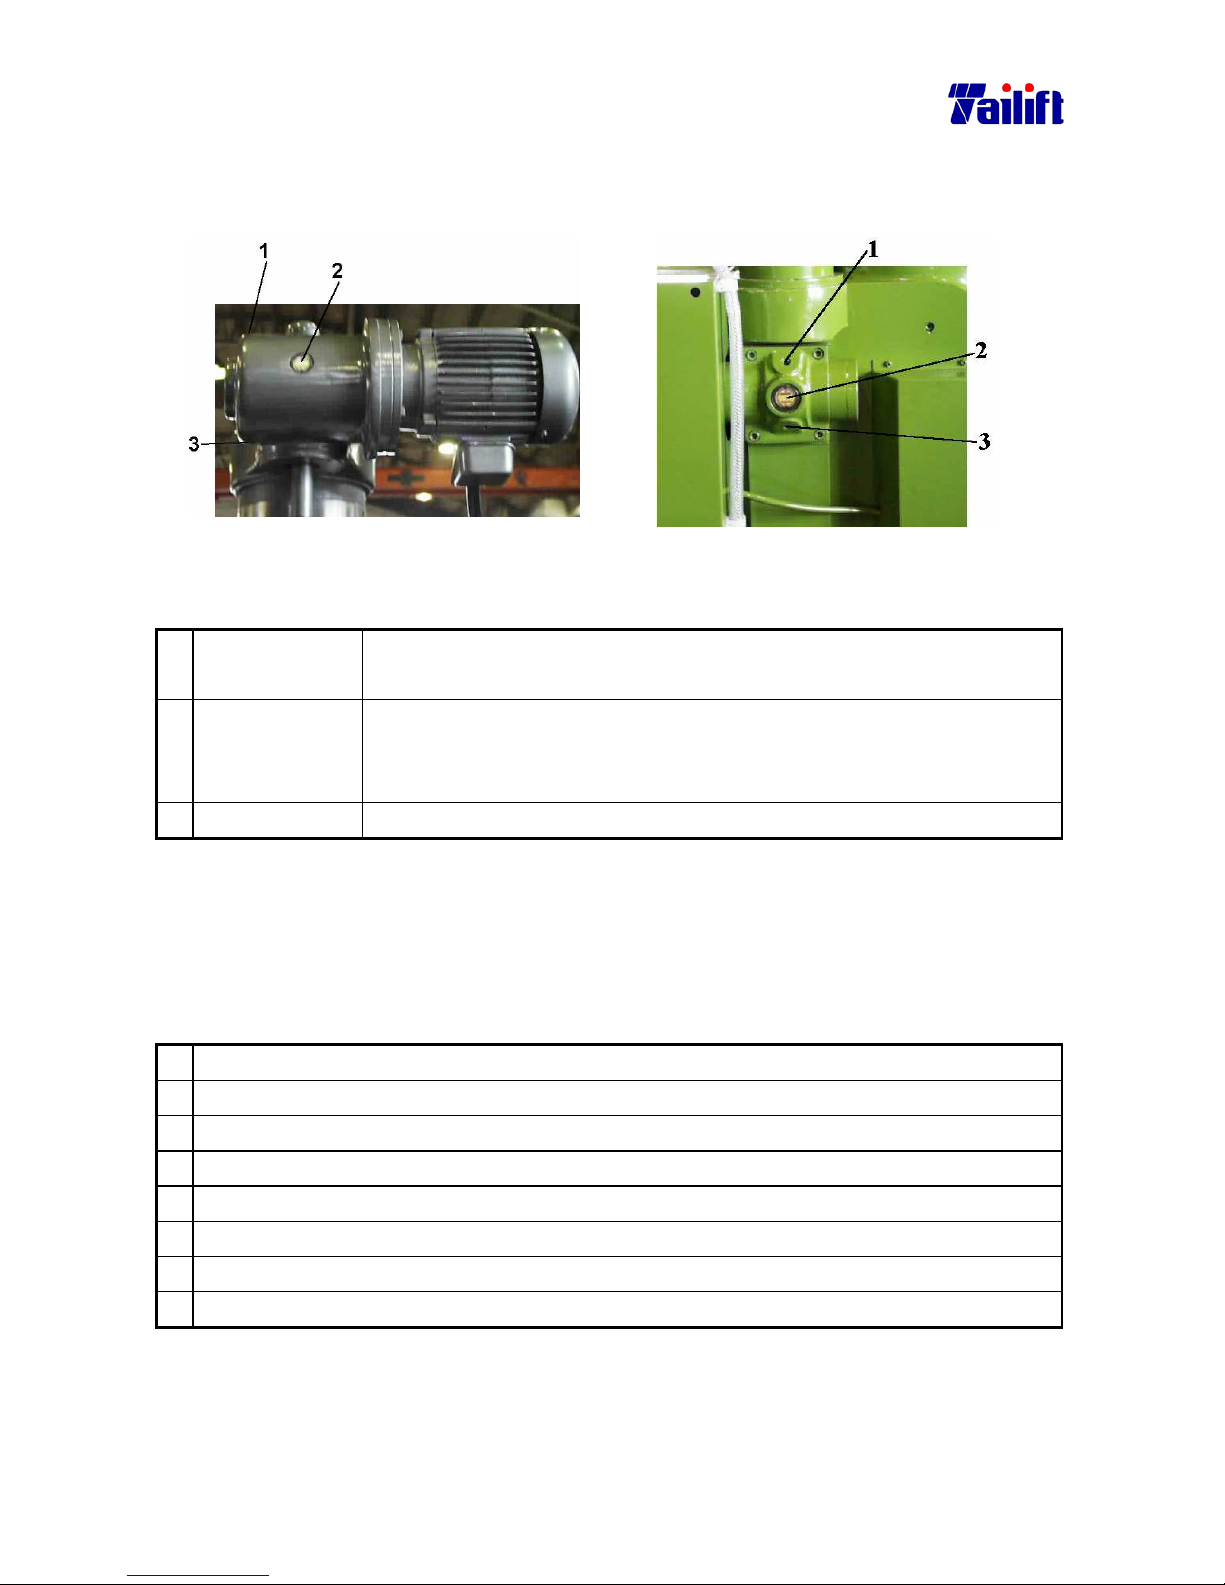
7.2.5 Change oil inside of the speed reduction of the arm elevating motor.
It requires only one person to do it. Please press down the emergent stop button and power
off before proceeding the job.
(For TPR-720A, TPR-820A, TPR-920A)
(For TPR-1100)
Instruction to the relevant parts.
1. Oil filler points It is the open where oil is added after the oil in the container isn’t
enough or needs to be replaced.
2. Oil gauge The volume of the oil is visible here. Generally, The oil level should be
between the upper and the lower lines. If it reaches the lower limit, oil
needs to be added, at the utmost to its upper line, but not over it.
3. Drain outlet It is to drain the oil when oil is to be replaced.
The following is the Tool to replace the oil.
Oil 2(CC68) L
Container and spanner.
The steps:
1. Power off.
2. Press down the emergent stop button.
3. Place the container under the drain outlet.
4. Release the drain plug using a spanner.
5. After draining, tape the plug with a sheet of band and tighten it back to the drain outlet.
6. Release the oil filler plug.
7. Add oil to the upper limit of the oil gauge.
8. Tighten the oil filler plug.
Page 67
7-5
7.2.6 Chang the oil inside the gearbox.
It calls for only one person to do it. Please power off and press down the emergent stop
button before carrying out the job.
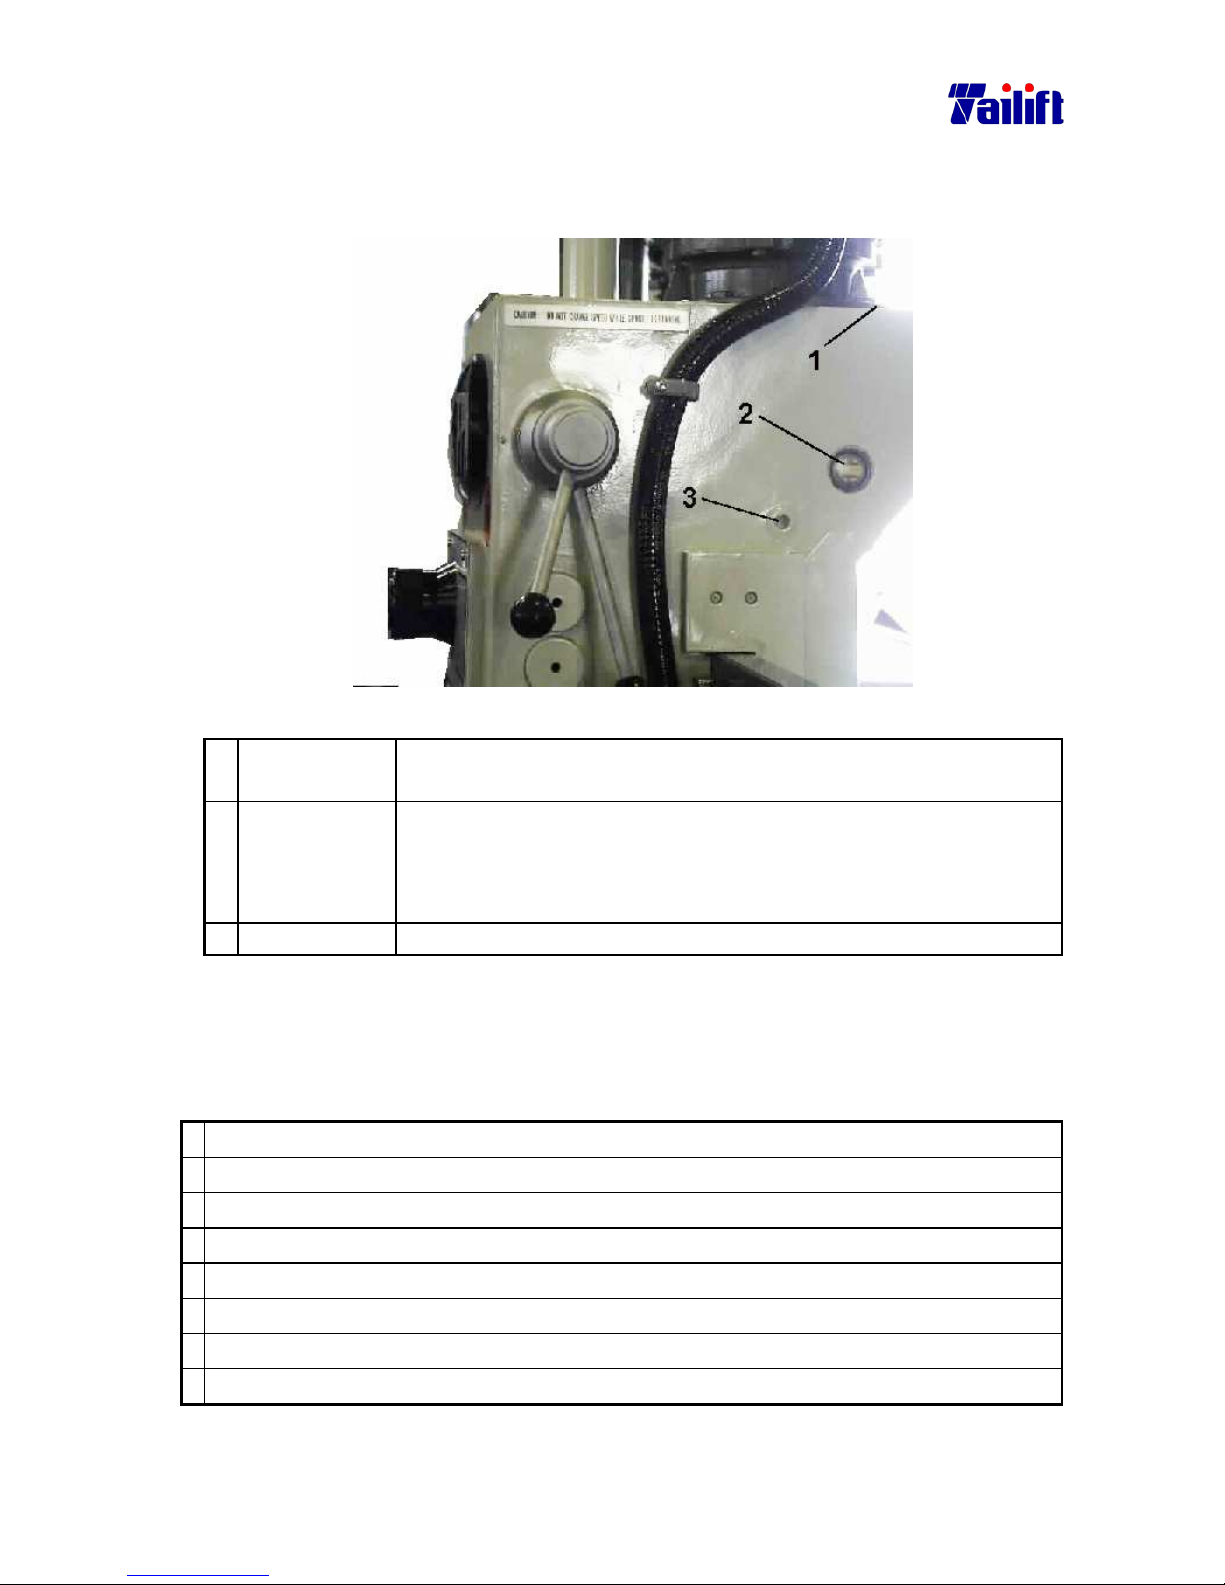
Instruction to the relevant parts.
1. Oil filler points It is the open where oil is added after the oil in the container isn’t
enough or needs to be replaced.
2. Oil gauge The volume of the oil is visible here. Generally, The oil level should
be between the upper and the lower lines. If it reaches the lower
limit, oil needs to be added, at the utmost to its upper line, but not
over it.
3. Oil drain outlet It is to drain the oil when oil is to be replaced.
The following is the Tool for replacing the oil.
Oil (CC68) 4.5 L
Container and spanner
The Steps::::
1. Power off.
2. Press down the emergent stop button.
3. Place a container under the oil drain outlet.
4. Release the drain plug using a spanner.
5. After draining, tape the plug with a sheet of band and tighten it back to the drain outlet.
6. Release the oil filler plug.
7. Add oil to the upper limit of the oil gauge.
8. Tighten the oil filler plug.
Page 68
7-6
7.3 Replace the cutting fluids.
It requires only one person to do it. Please power off and press down the emergent stop
power button before carrying out the job.
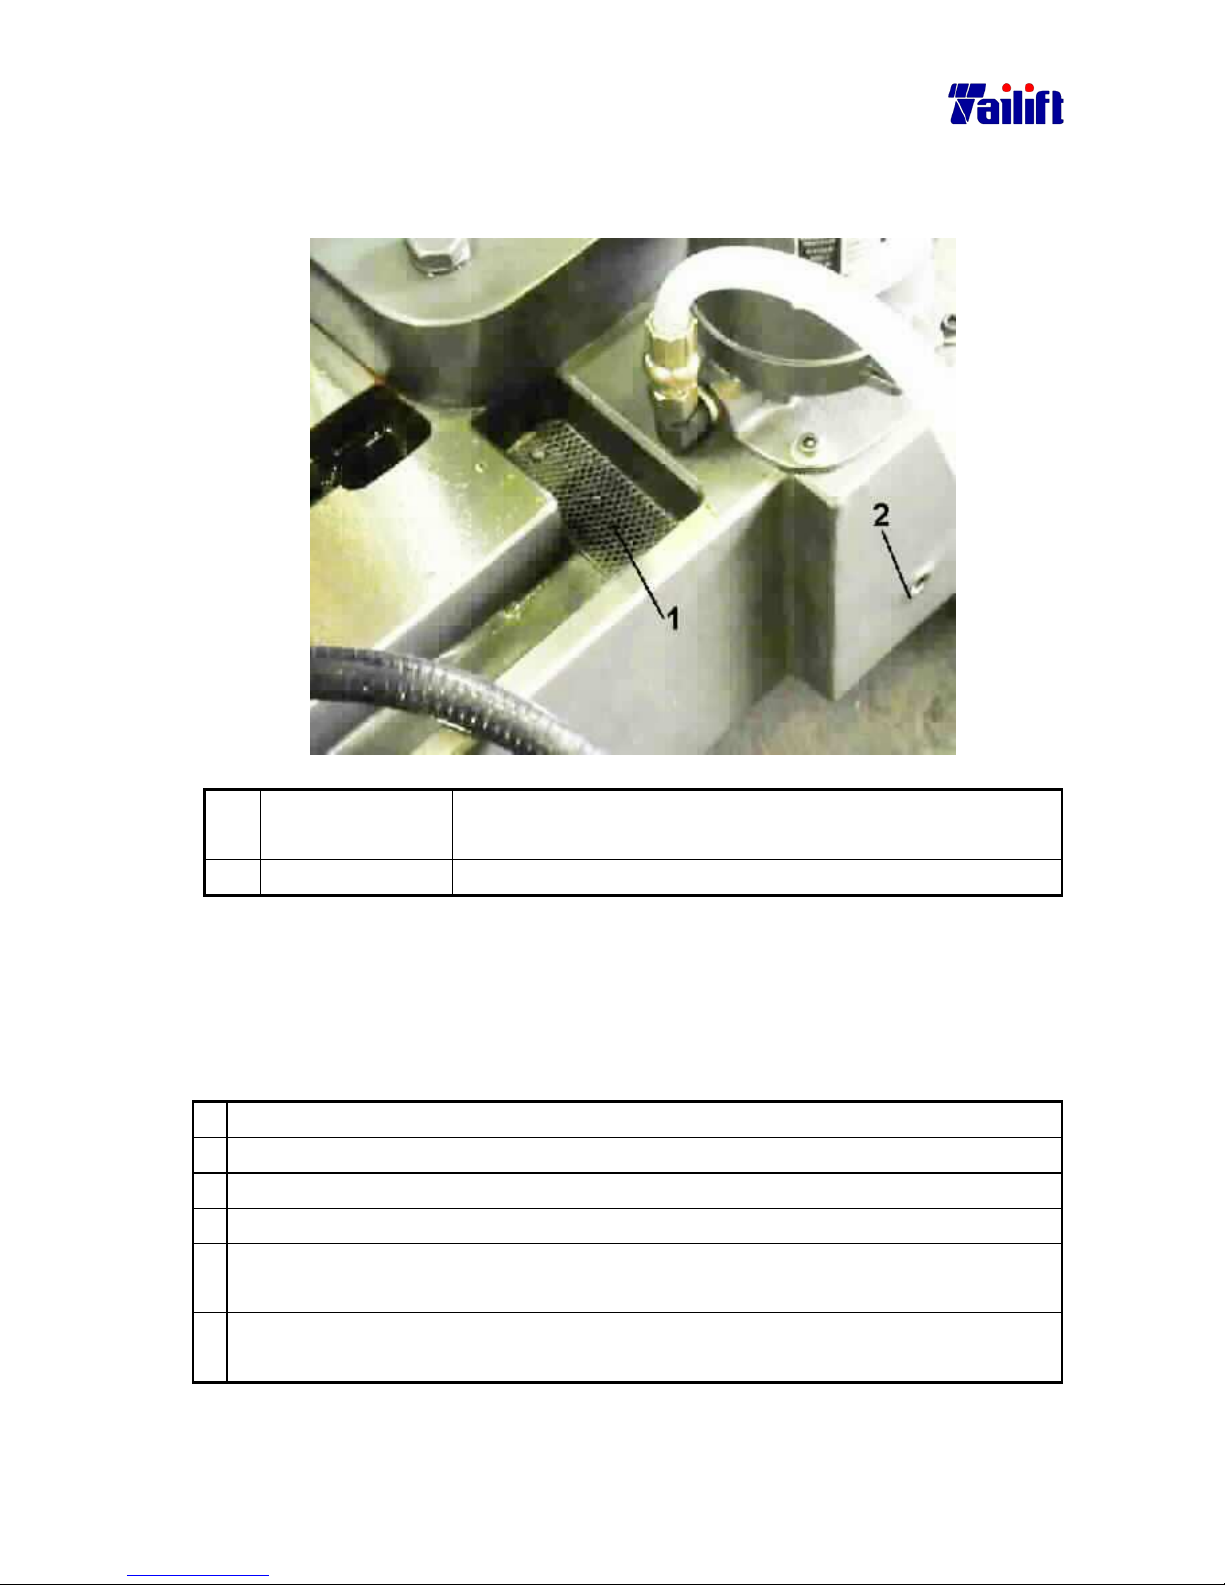
Instruction to the relevant parts.
1. Oil filler points It is the open where the cutting fluids are added when it
recycles, or isn’t sufficient or needs to be replaced.
2. Oil drain outlet It is the outlet where the cutting fluids are drained.
The following is the Tool to replace the cutting fluids.
The cutting fluids 30L
Container and spanner
The steps::::
1. Power off.
2. Press down the emergent stop button.
3. Place a container under the oil drain outlet.
4. Release the drain plug using a spanner.
5. After draining, tape the plug with a sheet of band and tighten it back to the drain
outlet.
6. Refill the cutting fluids through the oil filler inlet to the level under 5 mm under the
oil filter.
Page 69
7-7
7.4 Maintenance and replacement period.
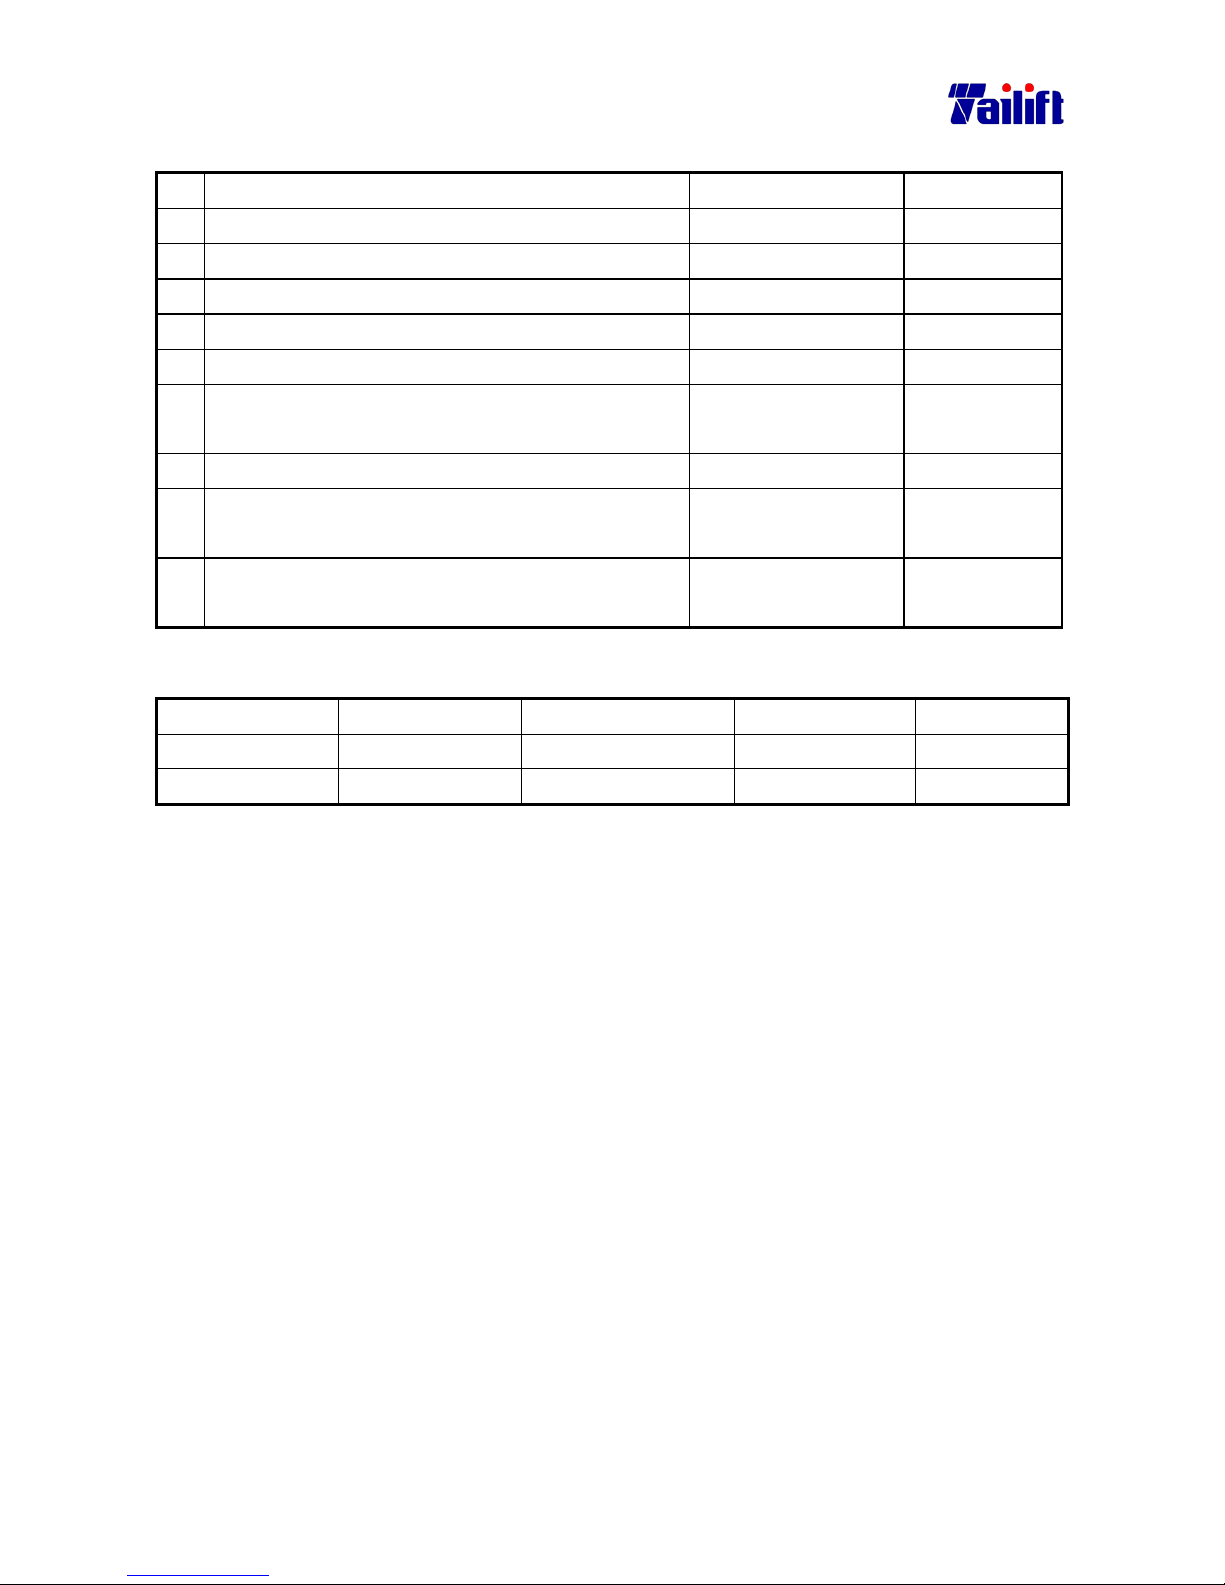
No.
Position Items. Period
1. Oil filler points of the column CC68 once per day.
2. Oil filler points on top of the gearbox CC68 once per day.
3. Oil filler points in the right side of the gearbox. CC68 once per day.
4. Oil filler points in the left side of the gearbox. CC68 once per day.
5. Oil filler points of the spindle XM2 once per day.
6 Replace oil for the speed reduction of the arm
elevating motor.
CC68 once per year.
7 Change oil inside of the gearbox. CC68 once per year.
8 Chang the cutting fluids. The cutting fluids once per
month.
9 The arm transmit ion ball screw XM2 Once per
month
A suitable Oil Type comparison:
ISO DIS-3498
SHELL MOBIL ESSO CHINA
CC68
OMALA 68
MOBILGEAR 620 SPARTAN EP68 HD68
XM2
ALVANIA R2 MOBILUX 2 BEACON 2 #2
7.5 Waste disposition.
Please proceed waste disposition such as machine oil, iron filings, old machine or replaced
parts according to your country’s relevant legal regulation.
Page 70
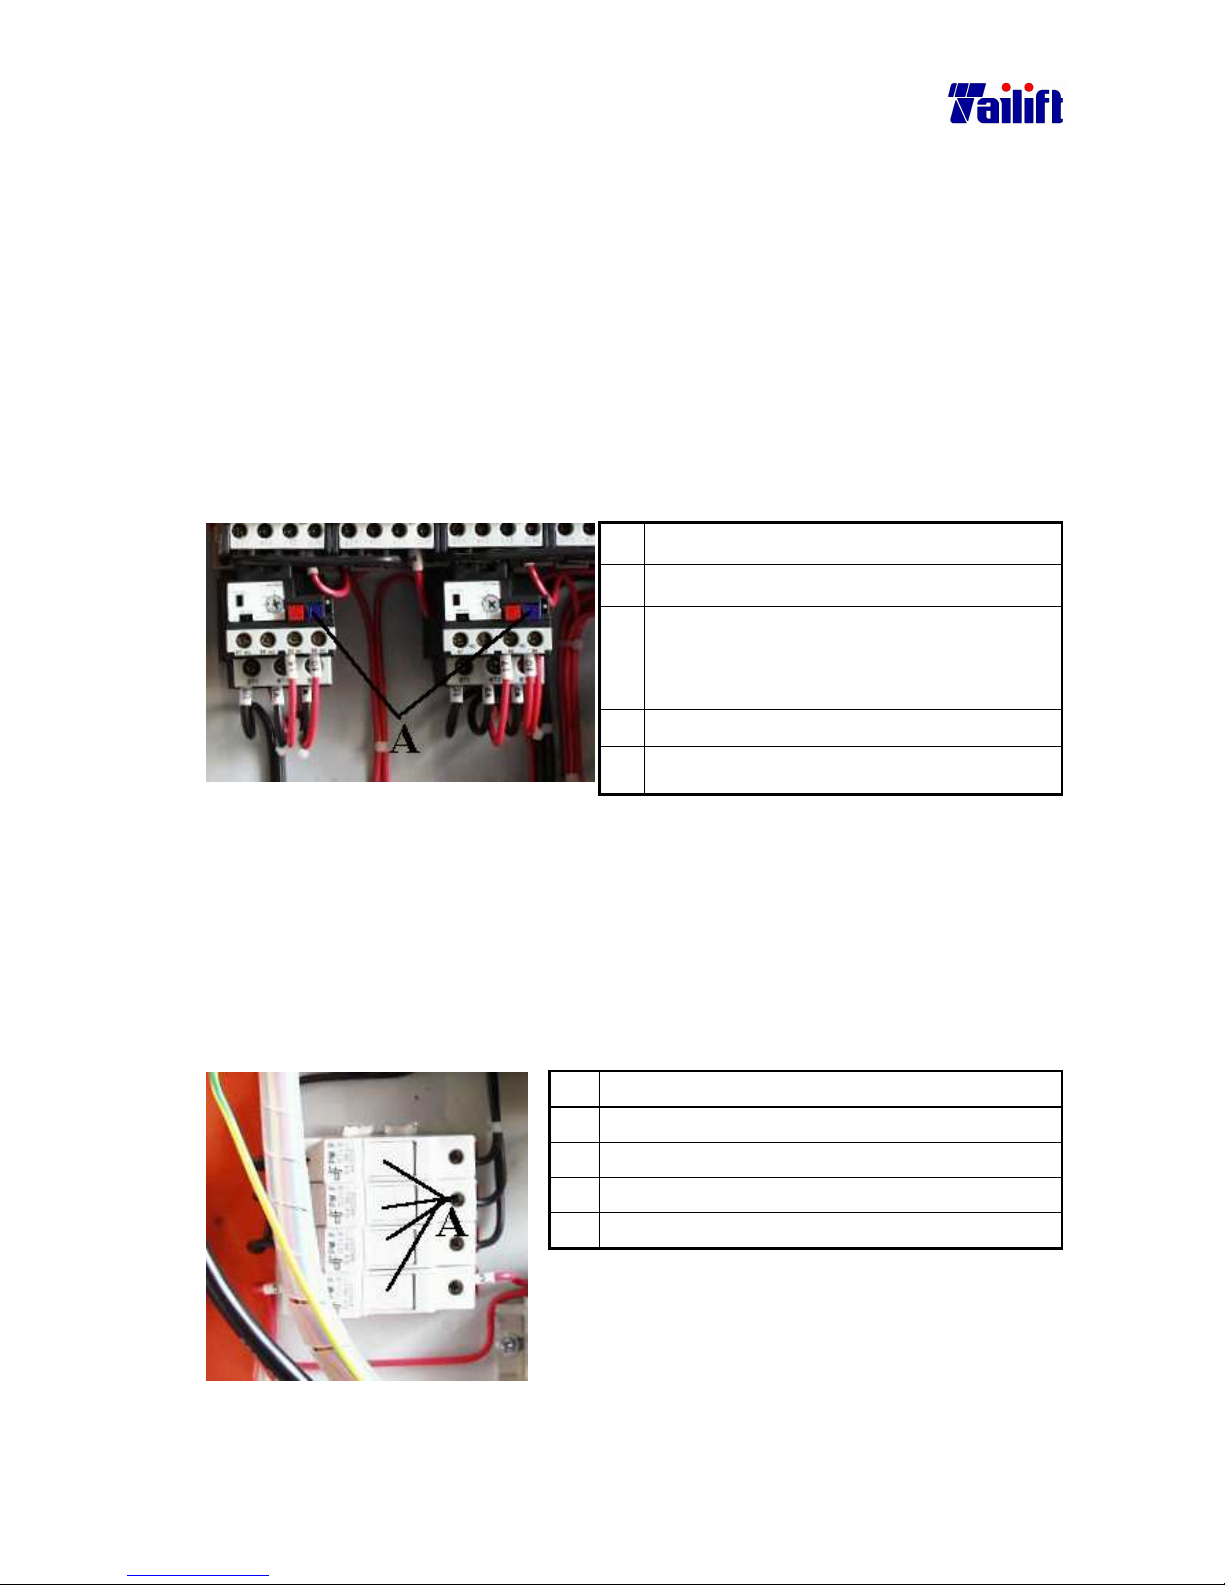
8-1
CHAPTER 8
Troubleshooting
8.1 The spindle overloads and the relay jumps.
8.1.1 The cause.
a. The drill bit is too big.
b. The feed rate is too fast.
c. Operation not in compliance with speedometer and the automatic feed rate table.
d. The fuse burned out.
e. The voltage is too low.
8.1.2The solution
a. Power off.
b. Open the control box.
c.
Press the relay switch to open, as shown in
the right picture, three minutes after the
spindle stops. (blue Button)
d. Close the control box.
e. Power on.
8.2 The spindle overloads and the fuse burns out.
8.2.1 The cause
a. The drill bit is too big.
b. The feed rate is too fast.
c. Operation not in compliance with speedometer and the automatic feed rate table.
8.2.2 The solution.
a. Power on.
b. Open the control box.
c. Replace the fuse as shown in the picture A.
d. Close the control box.
e. Power on.
Page 71
8-2
8.3 What if the drill bit get broken????
a. Stop the spindle.
b. Press down the emergent stop button.
c. Push the gearbox backwards.
d. Pinch the end of the broken bit with a pliers.
e. Rotate counter clockwise and pull it out upwards.
8.4 What if the screw tap get broken?
a. Stop the spindle.
b. Press down the emergent stop button.
c. Using thread releaser, rotate the screw tap counter clockwise till it comes out. If it is
impossible to pull it out, you may think to melt it out with EDM or declare it
unusable.
8.5 How if a person is entangled?
a.
Press down the emergent stop button.
b.
Power off.
c. Switch the speed change lever to the highest gear.
d. Rotate the spindle with hands counter clockwise (if the spindle moved clockwise
before, then its reverse direction is counter clockwise now) till that the person is free
from the machine.
Page 72
0-1
Section Content page
CHAPTER 1 Safety Guidelines….………………………………………………..
1-1
1.1 Please follow the below basic safety principles..………………………..
1-1
1.2 Precautions for the transportation and installation..……………………..
1-1
1.3 Precautions for operation....……………………………………………..
1-2
1.4 Precautions for checking and maintenance...……………………………
1-2
1.5
Warning labels and mark on the machine……………………………….
1-3
1.5.1
Warning labels and mark introduction ………………………………….
1-3
1.5.2 Labels Warning labels and mark positions ……………………………...
1-4
CHAPTER 2 General specifications………………………………………….…..
2-1
2.1 The anticipated machine life..…………………………………………...
2-1
2.2 Machine dimensions..…………………………………………………...
2-1
2.3 The machine...…………………………………………….……………..
2-2
2.3.1 Description….………………………………………………………..….
2-2
2.3.2 Parts...……………………………………………………………………
2-2
I For TPR-720A, TPR-820A, TPR-920A ………………………….
2-2
II only for TPR-1100………………………………………………..
2-3
2.4
Specifications
………………………………………………………….
2-4
2.4.1 TPR-720A ……………………………………………………………...
2-4
2.4.2 TPR-820A Specification ..……………………………………………...
2-5
2.4.3 TPR-920A specification ……………………………………………….
2-6
2.4.4 TPR-1100 specification ……………………………………………….
2-7
2.5
Standard and Option Accessories….…………………………………….
2-8
2.6 Operation position and noise level...…………………………………….
2-8
2.6.1 Operation position……………………………………………………….
2-8
2.6.2 The noise level...………………………………………………………...
2-8
CHAPTER 3 Preparation to install………………………………………………
3-1
3.1 Space and room requirement……………………………………………
3-1
3.1.1 Floor requirement………………………………………………………..
3-1
3.1.2 Space requirement...……………………………………………………..
3-2
3.2 Environment requirement...……………………………………………..
3-3
3.3 Power supply requirement...…………………………………………….
3-3
3.4 Electric system calculation……………………………………………...
3-4
CHAPTER 4 Transportation and Installation
….……………………………..
4-1
4.1 Disassembly and packaging..……………………………………………
4-1
4.1.1 General…………………………………………………………………..
4-1
4.1.2 Packaging………………………………………………………………..
4-1
Page 73
0-2
Section Content page
4.2 Transportation..……………………………………………………….…
4-2
4.2.1 The diagram of the machine weight and its gravity center...……………
4-2
4.2.2 The movement of the machine……. ……………………………………
4-2
4.2.3 The order to pack..………………………………………………………
4-3
4.3 Installation of the machine..……………………………………………..
4-4
4.3.1 Have the machine set onto the fastening bolts of the crate base...………
4-4
4.3.2 Level adjusting…………………………………………………………..
4-5
4.3.3 The installation of the electricity...……………………………………...
4-5
4.4 The test after installation………………………………………………...
4-6
4.5 The procedure for dismantling the machine…..………………………...
4-6
CHAPTER 5 Operation……………………………………………………………..
5-1
5.1 A brief introduction to the relevant operation hardware………………...
5-1
5.1.1 ( For TPR-720A, TPR-820A, TPR-920A)………………………………
5-1
5.1.2 ( For TPR-1100)…………………………………………………………
5-4
5.1.3 Safty protective device…………………………………………………..
5-7
5.2 Instruction to switches..…………………………………………………
5-8
I ( For TPR-720A, TPR-820A, TPR-920A)………………………………
5-8
II ( For TPR-1100)….……………………………………………………...
5-11
5.3
Installation of the clamp(work piece….……………………………….
5-12
5.3.1 General...………………………………………………………………...
5-12
5.3.2 Introduction of the vise and the clamping of the work piece...………….
5-12
5.3.3 Universal clamp and the clamping of the work piece…………………...
5-13
5.4 Installation and change of the drilling bit……………………………….
5-15
5.4.1 The assembly and disassembly of the drilling head and clamp...……….
5-16
5.4.2 The assembly and disassembly of the straight handle drill bit….………
5-18
5.5 Power on and off..……………………………………………………….
5-19
5.5.1 Power on..……………………………………………………………….
5-19
5.5.2 Power off..……………………………………………………………….
5-19
5.6 Work light..……………………………………………………………...
5-19
5.7 Cutting fluids...………………………………………………………….
5-19
5.8 Elevating the arm..………………………………………………………
5-20
5.9 Rotate the arm right or leftwards.……………………………………….
5-21
5.10 Rotate the arm to or backwards...……………………………………….
5-22
5.11 Change the spindle speed.……………………………………………….
5-23
5.11.1 For TPR-720A, TPR-820A, TPR-920A...……………………………….
5-23
I Speedometer...…………………………………………………………...
5-23
II Change spindle speed...………………………………………………….
5-24
5.11.2 For TPR-1100….………………………………………………………...
5-25
I The speedometer at the time when the pole switch is in high position….
5-25
II Change spindle speed…………………………………………………...
5-26
III The speedometer at the time when the pole switch is in low position…..
5-27
Page 74
0-3
Section
Content
page
5.12 Automatic Feed...………………………………………………………..
5-28
5.12.1 Automatic feed rate table………………………………………………..
5-28
5.12.2 Change the feed rate as the following way……………………………...
5-28
5.12.3 Suppose that the work piece is by the machine.………………………...
5-28
5.12.4 How to preset the depth of the power-feed..…………………………….
5-29
I (For TPR-720A, TPR-820A, TPR-920A)...……………………………
5-29
II (For TPR-1100)...…….………………………………………………...
5-30
5.13 The spindle………………………………………………………………
5-31
5.14 Threading.……………………………………………………………….
5-31
5.15 The assembly and disassembly of the work table...……………………..
5-32
5.16 Cutting fluids for all kinds of material…………………………………..
5-32
CHAPTER 6 Adjustment…………………………………………………………..
6-1
6.1 General...………………………………………………………………...
6-1
6.2 The arm clamping lever….……………………………………………...
6-1
6.3 The gap adjustment between the gearbox and the arm rail……………...
6-2
6.3.1 (For TPR-720A, TPR-820A, TPR920A)………………………………..
6-2
6.3.2 (For TPR-1100)….………………………………………………………
6-3
6.4 Adjust the engagement between the feed trip lever and the clutch……...
6-4
CHAPTER 7 Maintenance………………………………………………………….
7-1
7.1 General…………………………………………………………………..
7-1
7.2 Daily Maintenance..……………………………………………………..
7-1
7.2.1 Clearing...………………………………..………………………………
7-1
7.2.2 Please clean every parts using a metal brush and a rag, dipped with oil,
to rub them ……………………………………………………………...
7-1
7.2.3 The way to clean iron filings..…………………………………………..
7-2
7.2.4 Lubrication..……. ………………………………………………………
7-3
7.2.5 Change oil inside of the speed reduction of the arm elevating motor…..
7-4
7.2.6 Chang the oil inside the gearbox...………………………………………
7-5
7.3 Replace the cutting fluids………………………………………………..
7-6
7.4 Maintenance and replacement period….………………………………..
7-7
7.5 Waste disposition..………………………………………………………
7-7
CHAPTER 8 Troubleshooting…………………………………………………….
8-1
8.1 The spindle overloads and the relay jumps...……………………………
8-1
8.1.1 The cause..………..……………………………………………………..
8-1
8.1.2 The solution..………..…………………………………………………..
8-1
8.2 The spindle overloads and the fuse burns out….………………………..
8-1
Page 75
0-4
Section Content page
8.2.1 The cause………………………………………………………………..
8-1
8.2.2 The solution.………...…………………………………………………..
8-1
8.3
What if the drill bit get broken?.……………………………………….
8-2
8.4 What if the screw tap get broken?...……………………………………..
8-2
8.5 How if a person is entangled?..………………………………………….
8-2
CHAPTER 9 Annex
9.1 Electrical circuit diagram(TPR720A,TPR820A,TPR920A CE Standard)
9-1
9.2 Electrical circuit diagram(TPR1100 CE Standard)……………………...
9-2
9.3 Electrical main part list(TPR720A,TPR820A,TPR920A CE Standard)...
9-3
9.4 Electrical main part list (TPR1100 CE Standard)……………………….
9-4
9.5 Earth System Diagram(TPR720A,TPR820A,TPR920A CE Standard)…
9-5
9.6 Electrical circuit diagram(TPR720A,TPR820A,TPR920A Standard)…..
9-6
9.7 Electrical main part list (TPR720A,TPR820A,TPR920A Standard)……
9-7
9.8 Electrical circuit diagram(TPR1100 Standard)………………………….
9-8
9.9 Electrical main part list (TPR1100 Standard)…………………………...
9-9
Page 76
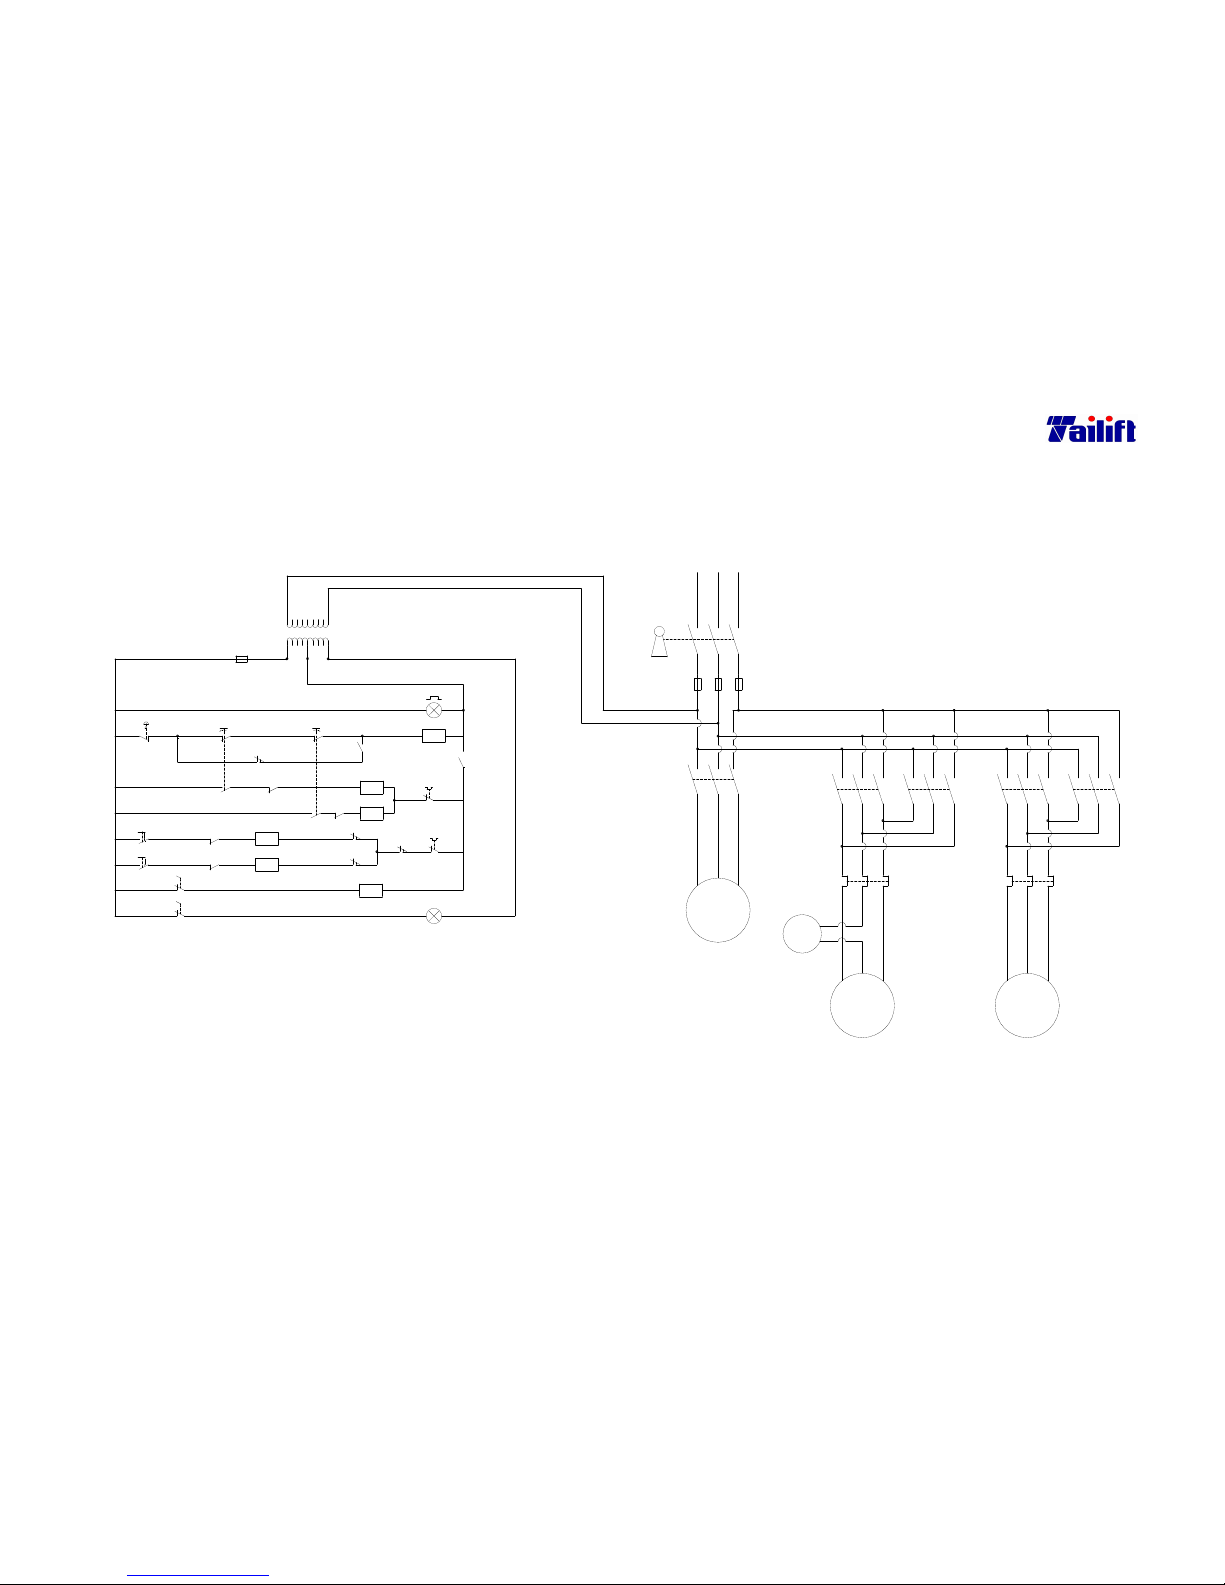
9-1
CHAPTR 9 Annex
9.1 Electrical circuit diagram
(For TPR720A,TPR820A,TPR920A CE Standard)
FU3
M1
L11
L21
FU1
L12
L22
FU2
M2
2mm
Key Switch
2mm2mm
2 2
L1 L22L3
2mm
OL1
2mm
2
2
2mm
2
M3
2mm
2
2
2mm
2
2mm
2
2mm
2
2mm
2
2mm22mm
2 2
2mm
2mm
2mm22mm
2 2
2mm
M4
2mm
2
2mm
OL2
2mm22mm
M5
2 2
2mm
2
2mm
2
2mm22mm
2
2
M2
3~
Elevating
0.75Kw
Motor
5
M0
2
Control
Relay
10
5
5
10
LS4
18
1.25mm
2
1.25mm
2
UP
Elevating
12
11
SS3(Cross Switch)
5
SS3(Cross Switch)
20
SS2
U1,V1,W1
4
(4)
M4
LS3
M0
1.25mm
1.25mm
110V
5
0V
1.25mm
2
5
24V
LS1
1.25mm
M4
SS1
6
3
1
SS3(Cross Switch)
13
FU4
7
1.25mm
1.25mm
2
1.25mm
(3)
2
M5
(1)
2
M2
M2
LS2
M1
(2)
2
M3
M3
SS3(Cross Switch)
4
2
8
400V
TR
150VA
19
2
1.25mm
(Alarm Lamp)
Work Lamp
Pump Motor
OL2
OL1
15
Coolant
Spindle
Reverse
Forward
Spindle
M0
2
1.25mm
1
2
1.25mm
2
2
9
9
Power
U,V,W
U2,V2,W2
1.25mm
1.25mm
2
2
A
2mm
1.5Kw
Main
Motor
M1
Pump Motor
0.1Kw
2mm
M3
3~
Coolant
2mm
2
~
2mm
2 2
3~
2mm
2
2
2mm
2
2mm
L13
L23
PB1
17
M3
Page 77
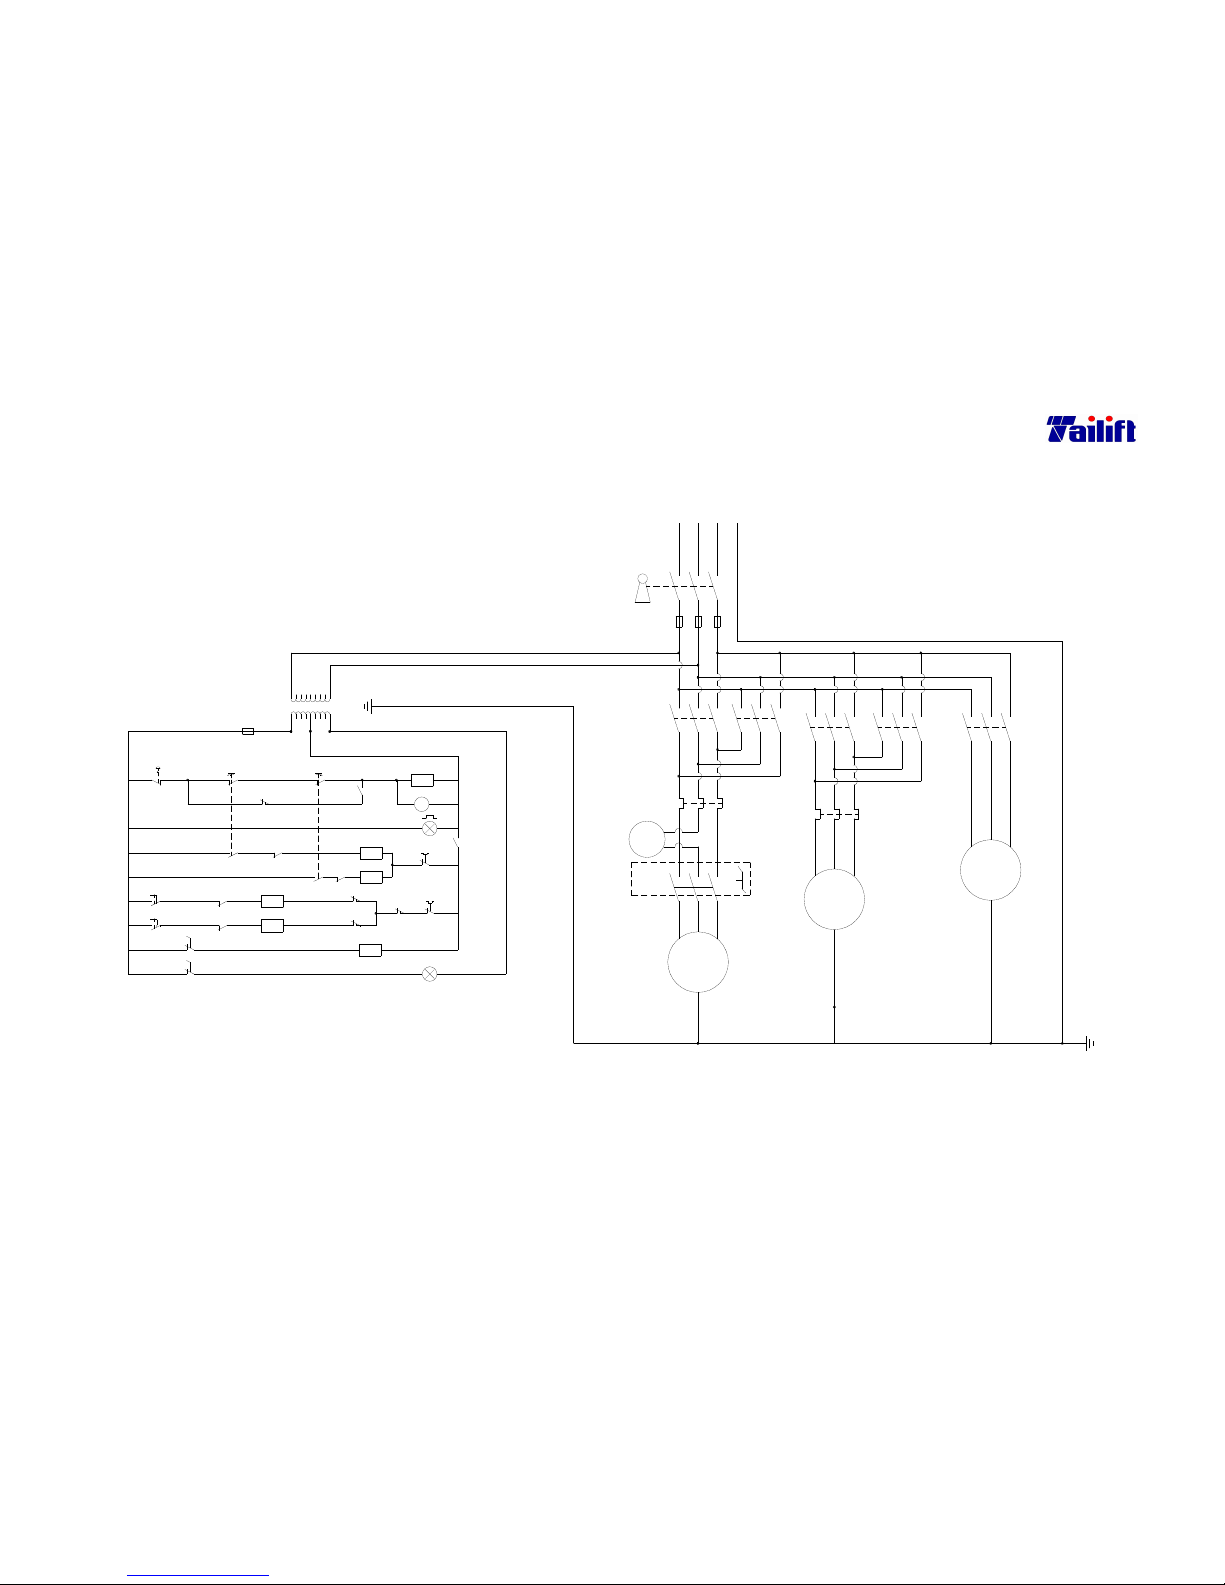
9-2
9.2 Electrical circuit diagram
(For TPR-1100 CE Standard)
PB1
17
M3
4
(4)
M4
LS3
M0
1.25mm
1.25mm
5
1.25mm
2
5
LS1
1.25mm
M4
SS1
6
3
1
SS3(Cross Switch)
13
FU4
7
1.25mm
1.25mm
2
1.25mm
(3)
2
M5
(1)
2
M2
M2
LS2
M1
(2)
2
M3
M3
SS3
4
2
8
19
2
1.25mm
Work Lamp
Pump Motor
OL1
OL1
15
Coolant
Spindle
Reverse
Forward
Spindle
M0
2
1.25mm
1
2
1.25mm
2
2
9
9
U,V,W
U2,V2,W2
5
M0
2
10
5
5
10
LS4
18
1.25mm
2
1.25mm
2
UP
Elevating
12
11
SS5
5
20
SS2
U1,V1,W1
380V
PL
Elevating
DOWN
SS4
SS6
110V
0V
24V
220V
TR
E
150VA
1.25mm
1.25mm
2
2
A
1.25mm
0.75Kw
Elevator
Motor
M2
Motor
1.5Kw
2mm
M1
3~
Main
2mm
2
~
2mm
2 2
1.25mm
2
2
1.25mm
3~
1.25mm
2 2
1.25mm
2
M3
0.1Kw
Coolant Pump
Motor
3~
L13
FU3
M3
L11
FU1
L12
FU2
OL1
M2
M5
3.5mm
Key Switch
3.5mm3.5mm
2 2
L1 L2
2
3.5mm
2
PEL3
OL2
M4
1.25mm
M1
U
1.25mm1.25mm
W
22V2
W1V1U1
U2 V2 W2
Page 78
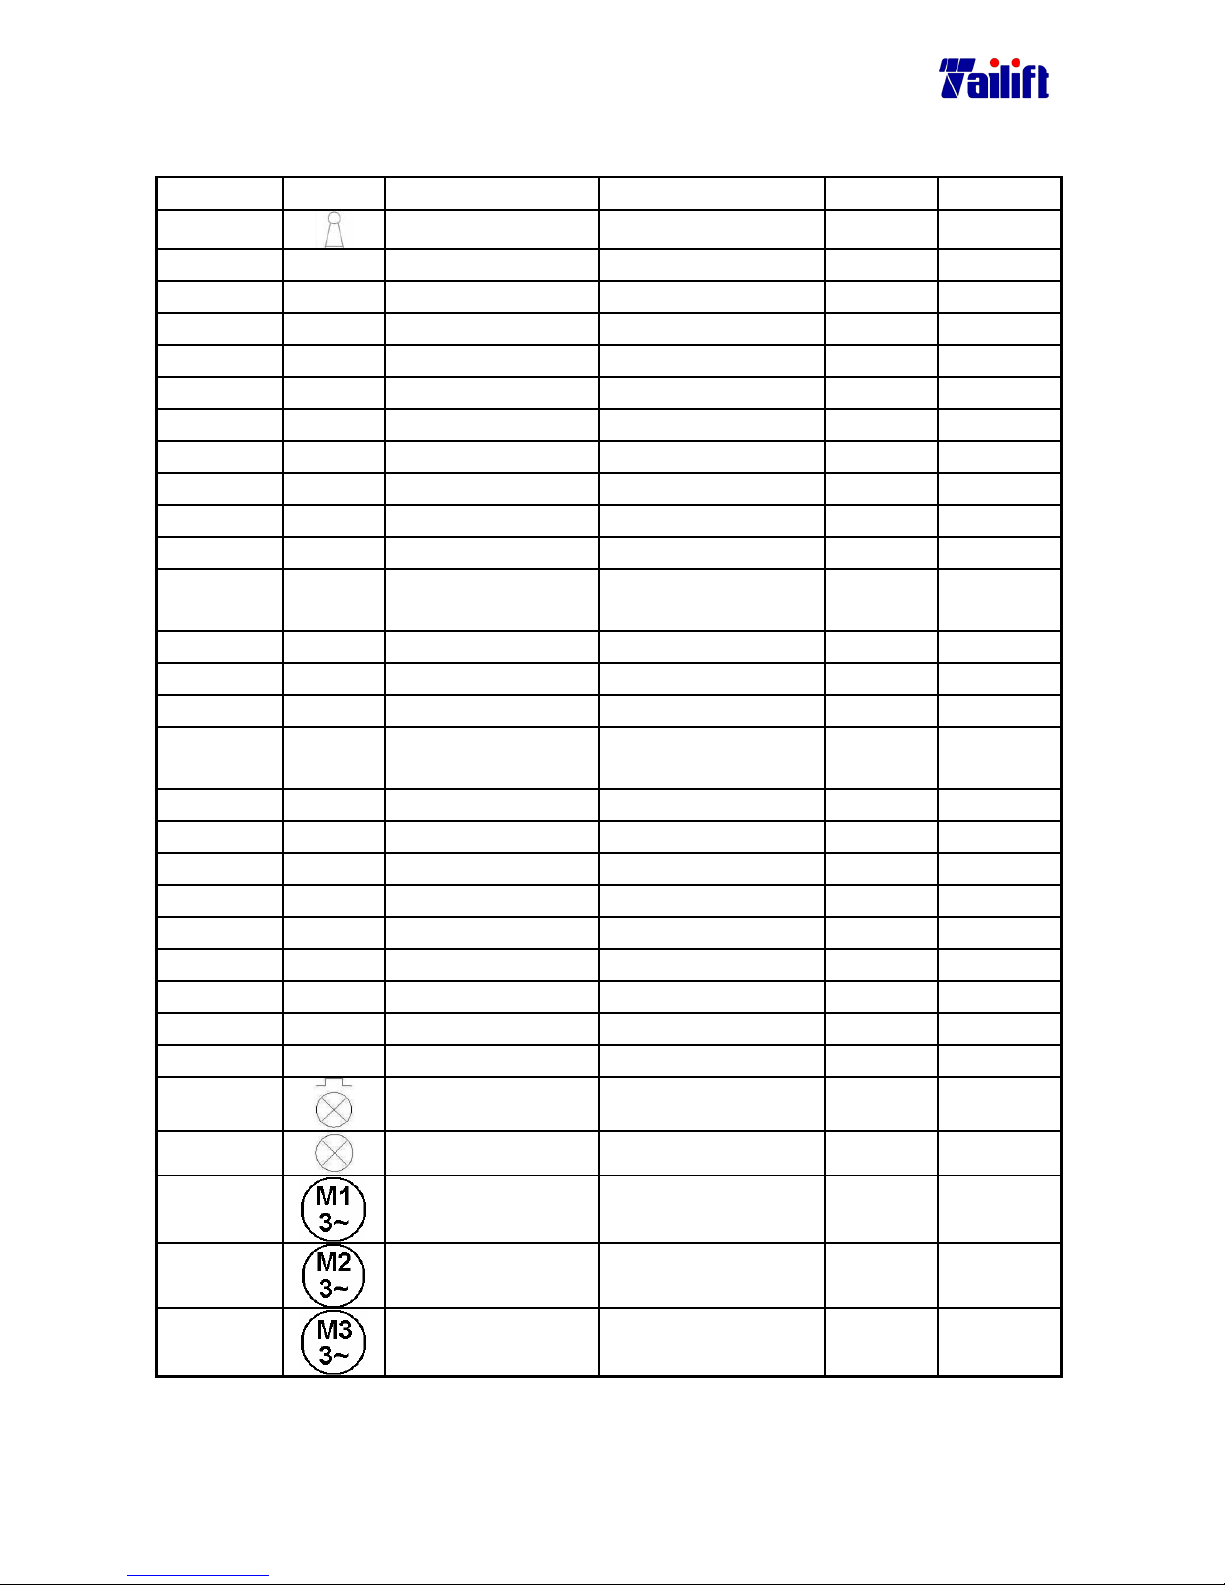
9-3
9.3 Eletrical main parts list
(For TPR-720A, TPR-820A, TPR-920A CE Standard )
Part NO. Symbol
Name Specification Q’ty Remark
E1602001
Key Switch XF 163B 1
E0703001 M1 Magnetic Contact CN11 3a1b 24V 1
E0703001 M2 Magnetic Contact CN11 3a1b 24V 1
E0703001 M3 Magnetic Contact CN11 3a1b 24V 1
E0703001 M4 Magnetic Contact CN11 3a1b 24V 1
E0703001 M5 Magnetic Contact CN11 3a1b 24V 1
E0703001 M0 Magnetic Contact CN11 3a1b 24V 1
E3101023 FU1 Fuse 10*38*16A 1
E3101023 FU2 Fuse 10*38*16A 1
E3101023 FU3 Fuse 10*38*16A 1
E3101025 FU4 Fuse 10*38*6A 1
E1801020 TR Transformer 150VA
1:0,220,380 2:0,24,110
1
E1302004 SS1 Selector Switch YK∅∅∅∅22 1A1B 1
E1604001 SS2 Selector Switch SN1021 1
E0901021 SS3 Limit Switch V-15-1E5 4
E1605001 SS3 Cross Switch UP:1A,Down:1A,LEF
T:1A1B,RIGHT:1A1B
1
Option
B100006 SS4 Push button ZB4-BA2+ZB4-BZ101
1
B100006 SS5 Push button ZB4-BA2+ZB4-BZ101
1
E1303002 PB1 Emg. Push Button YK∅∅∅∅30 1A1B 1
E0207016 OL1 Overload Relay RHN 10/3.5~5 1
E0207014 OL2 Overload Relay RHN 10/1.4~2.1 1
E0901021 LS1 Limit Switch V-15-1E5 1
E0901014 LS2 Limit Switch MJ2-1308 1
E0901014 LS3 Limit Switch MJ2-1308 1
E0901014 LS4 Limit Switch MJ2-1308 1
E2305002
Power (Alarm Lamp) YK∅∅∅∅22 24V(W) 1
E1701002
Work Lamp FS 51441 110V 1
Main Motor 1.5KW
200/400V/4P/3PH
1
Elevating Motor 0.75KW
200/400V/4P/3PH
1
Coolant Pump Motor 0.1KW
200/400V/2P/3PH
1
Page 79
9-4
9.4 Eletrical main parts list
(For TPR-1100 CE Standard)
Part NO. Symbol
Name Specification Q’ty
Remark
E1602001
Key Switch XF 163B 1
E0703001 M1 Magnetic Contact CN11 3a1b 24V 1
E0703002 M2 Magnetic Contact CN18 24V 1
E0703002 M3 Magnetic Contact CN18 24V 1
E0703001 M4 Magnetic Contact CN11 3a1b 24V 1
E0703001 M5 Magnetic Contact CN11 3a1b 24V 1
E0703001 M0 Magnetic Contact CN11 3a1b 24V 1
E3101027 FU1 Fuse 10*38*20A 1
E3101027 FU2 Fuse 10*38*20A 1
E3101027 FU3 Fuse 10*38*20A 1
E3101027 FU4 Fuse 10*38*2A 1
E1801020 TR Transformer 150VA
1:0,220,380V
2:0,24,110V
1
E1203001 SS1 Selector Switch YK∅∅∅∅30 1A1B 1
E1604001 SS2 Selector Switch SN1021 1
E0901021 SS3 Limit Switch V-15-1E5 4
E1605001 SS3 Cross Switch UP:1A,Down:1A,LEF
T:1A1B,RIGHT:1A1B
1
Option
E1603001 SS4 Change Switch A441CA10 1
B100006 SS4 Push button ZB4-BA2+ZB4-BZ101
1
B100006 SS5 Push button ZB4-BA2+ZB4-BZ101
1
E1618003 PB1 Emg. Push Button YK∅∅∅∅30 1B 1
E0207017 OL1 Overload Relay RHN 10/5.5~8.5 1
E0207014 OL2 Overload Relay RHN 10/1.4~2.1 1
E0901006 LS1 Limit Switch MJ2-1308R 1
E0901014 LS2 Limit Switch MJ2-1308 1
E0901014 LS3 Limit Switch MJ2-1308 1
E0901009 LS4 Limit Switch MN 5311 1
E2305002
Power (Alarm Lamp) YK∅∅∅∅22 24V(W) 1
E2305001
Pilot YK∅∅∅∅30 24V(W) 1
E1701002
Work Lamp FS 51441 110V 1
Main Motor
1.5KW 200/400V/4P/3PH
1
Elevating Motor
0.75KW 200/400V/4P/3PH
1
Page 80
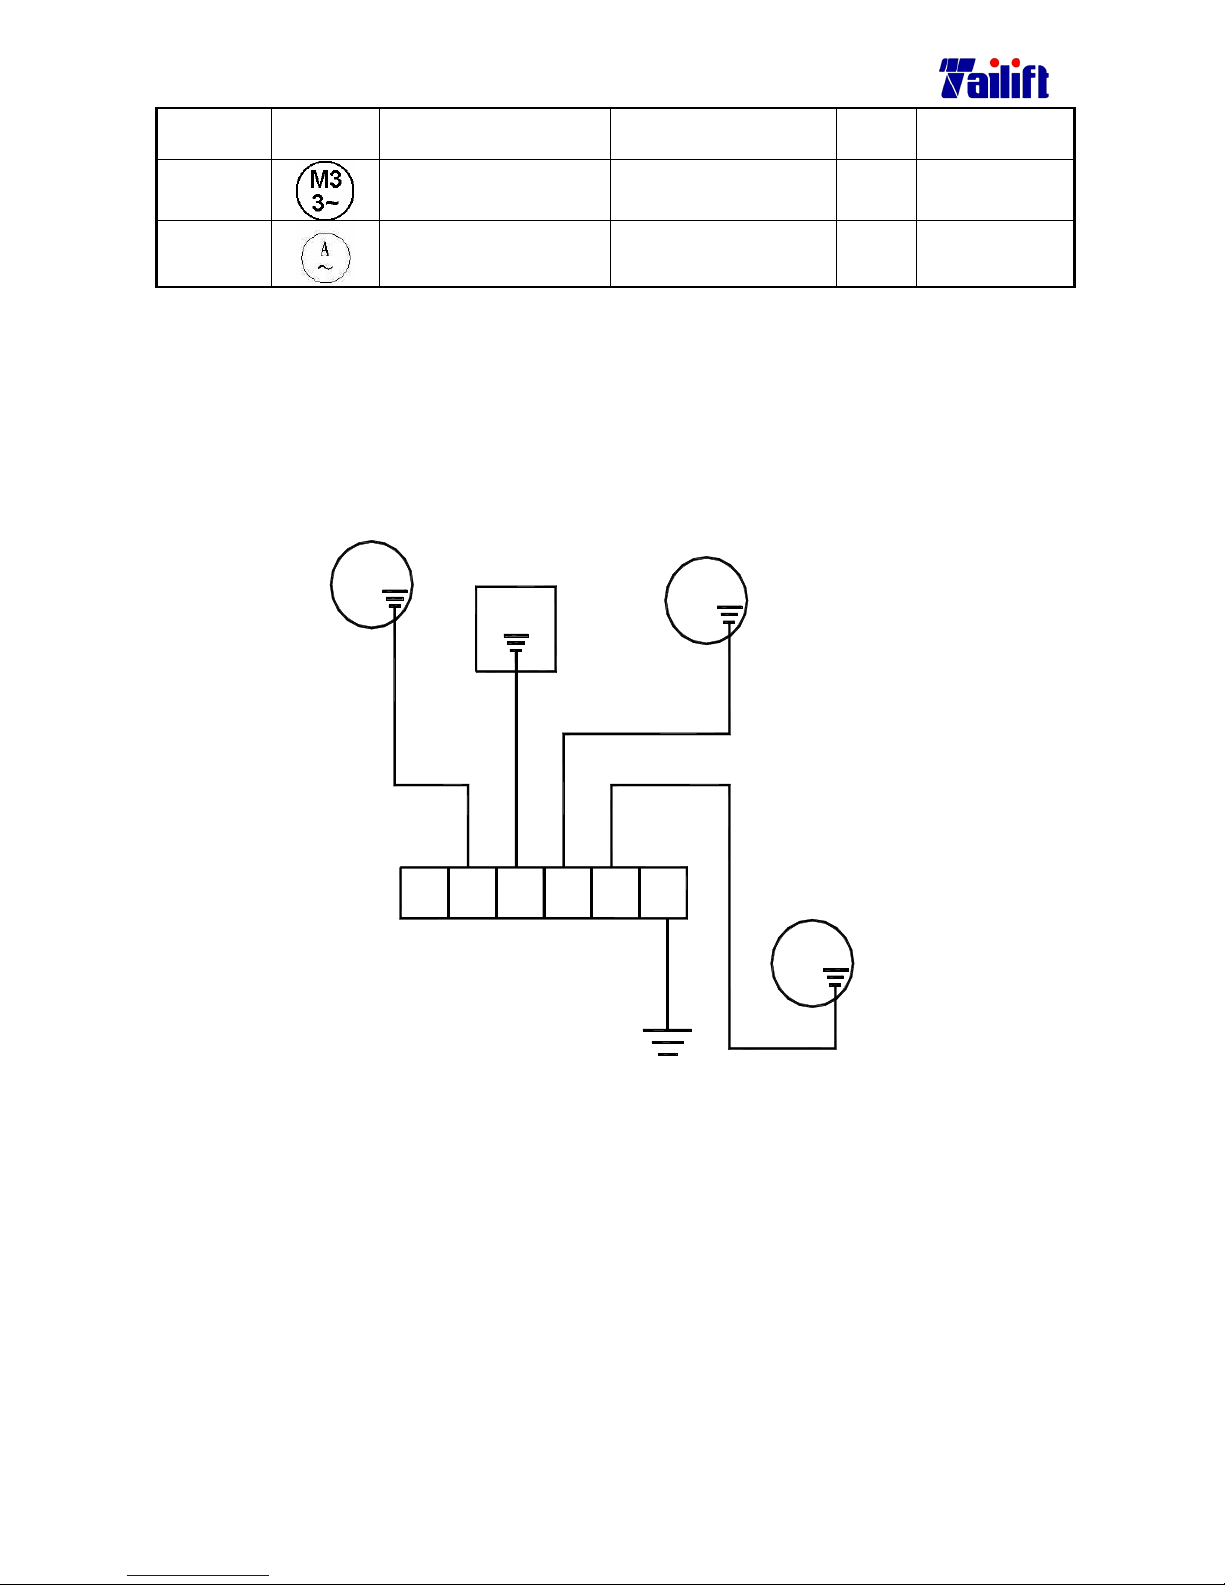
9-5
Part NO. Symbol
Name Specification Q’ty
Remark
Coolant Pump Motor 0.1KW
200/400V/2P/3PH
1
E3602002
AMP meter S065 20A 1
9.5 Earth System Diagram
(For TPR720A,TPR820A,TPR920A,TPR1100A CE Standard)
E E E E PE
M1
3~
TR
3~
M2
M3
3~
Page 81
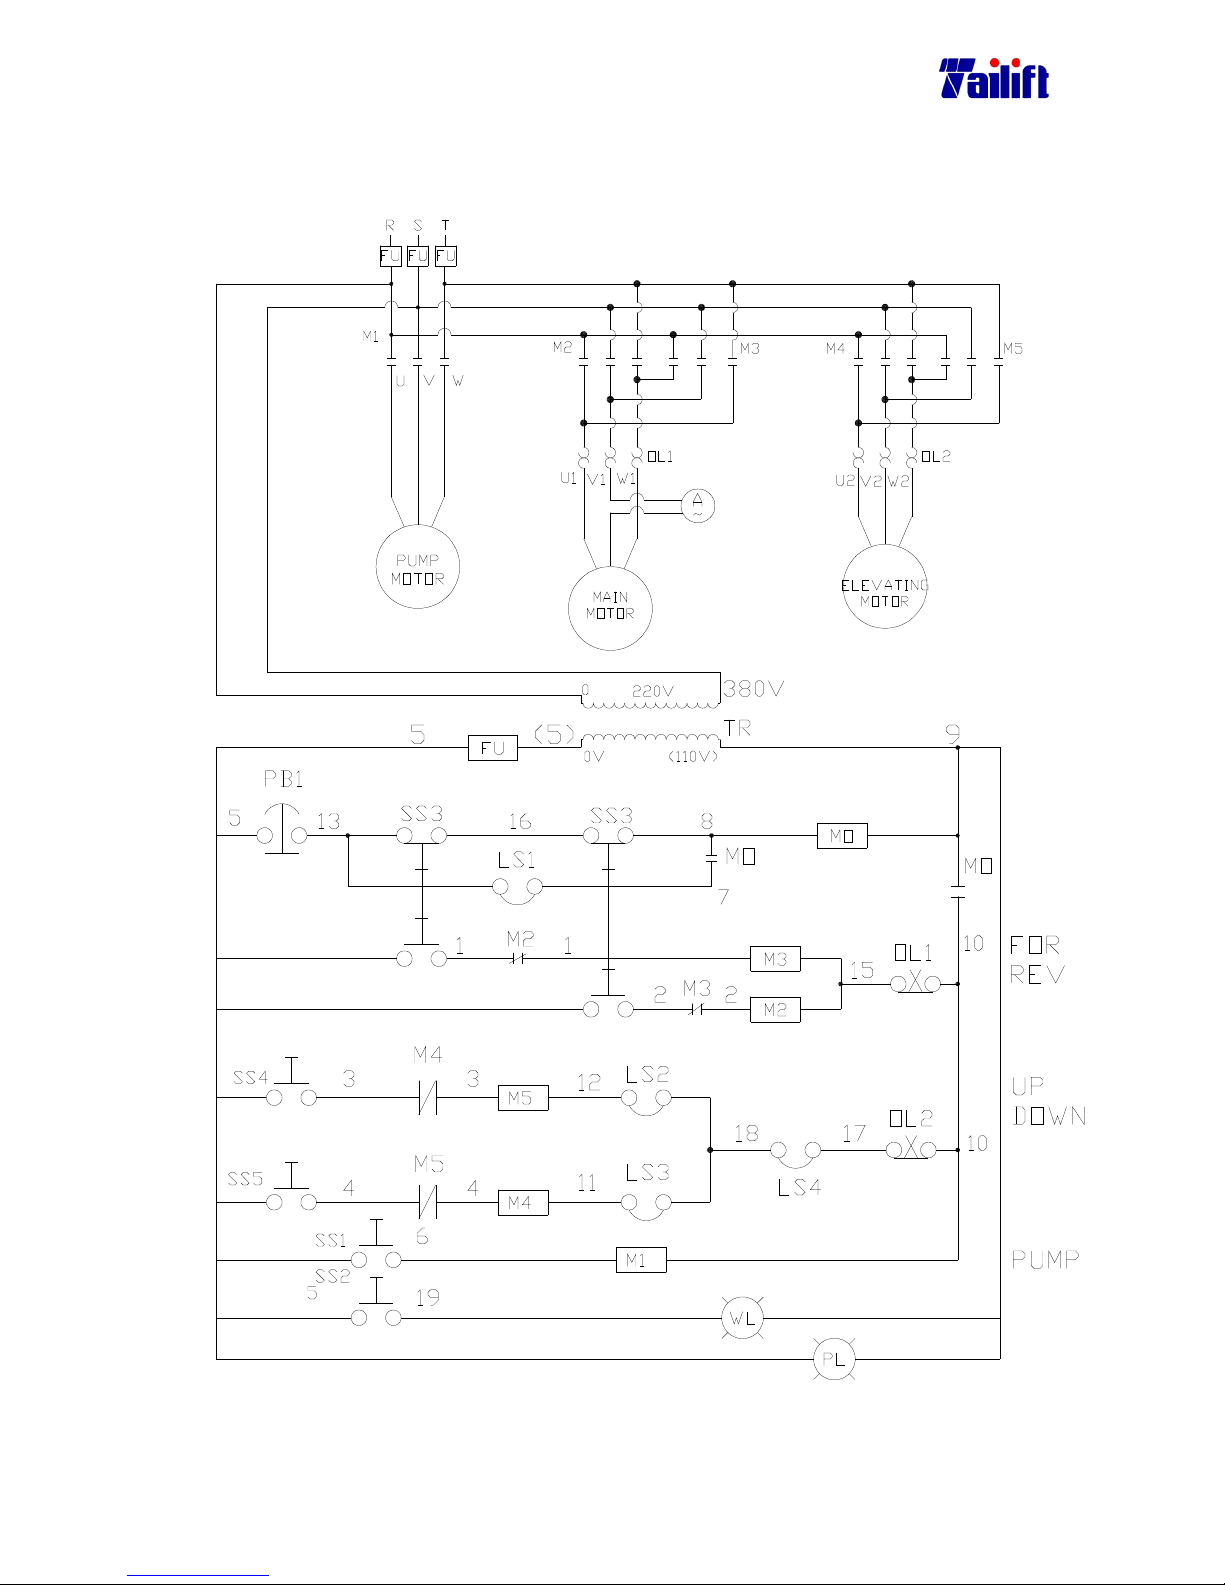
9-6
9.6 Electrical Circuit Diagram
(For TPR720A,TPR820A,TPR920A Standard)
Page 82
9-7
9.7 Eletrical main parts list
(For TPR-720A, TPR-820A, TPR-920A Standard )
Part NO. Symbol
Name Specification Q’ty
Remark
E0701006 M1 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M2 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M3 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M4 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M5 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M0 Magnetic Contact CN11 3a1b 110V 1 Standard
E3101010 FU Fuse E16 30A 3 For Asia
E3101013 FU Fuse E16 6A 1 For Asia
E1801005 TR Transformer PT40 1 Standard
E0207011 OL1 Overload Relay RH 18/7 1 For 220V~230V
E0207007
OL1 Overload Relay RH 18/4 1 For 380V~460V
E0207007
OL2 Overload Relay RH 18/4 1 For 220V~230V
E0207008
OL2 Overload Relay RH 18/1.7 1 For 380V~460V
E1618001 PB1 Emg.Push Button
Switch
SBT-307 1
Standard
E1304001
SS1 Selector Switch ST 251 1 Standard
E1604001
SS2 Selector Switch SN1021 1 Standard
E1605001
SS3 Cross Switch 3Joint.UP1A.Down1A
Left1A1B.Right1A1B
1
Option
E0901021 SS3 Limit Switch V-15-1E5 4 Standard
B100006 SS4 Push button ZB4-BA2+ZB4-BZ101
1 Standard
B100006 SS5 Push button ZB4-BA2+ZB4-BZ101
1 Standard
E0901021
LS1 Limit Switch V-15-1E5 1 Standard
E0901014
LS2 Limit Switch MJ2-1308 1 Standard
E0901014
LS3 Limit Switch MJ2-1308 1 Standard
E0901014
LS4 Limit Switch MJ2-1308 1 Standard
E1701002
WL Work Lamp FS51441 1 Standard
E2303002
PL Pilot Light SP-251 110V 1 Standard
E3602002
Amp Meter S065 20A 1
For 200V~230V
E3602003
Amp Meter S065 10A 1
For 380V~460V
Coolant Pump
Motor
1/8HP/2P/3PH
L:130mm
1
Standard
Main Motor Vertical 2HP/4P/3PH
1 Standard
Elevating Motor Horizontal
1HP/4P/3PH
1
Standard
Page 83
9-8
Part NO. Symbol
Name Specification Q’ty
Remark
E0703001
M1 Magnetic Contact CN18 24V 1
Optional
E0703001
M2 Magnetic Contact CN18 24V 1
Optional
E0703001
M3 Magnetic Contact CN18 24V 1
Optional
E0703001
M4 Magnetic Contact CN18 24V 1
Optional
E0703001
M5 Magnetic Contact CN18 24V 1
Optional
E0703001
M0 Magnetic Contact CN18 24V 1
Optional
E3101016 FU Fuse 5A(41*51) 1
For u.s.a
E3101014 FU Fuse 30A(41*51) 1
For u.s.a
E3101022 FU Fuse 10*38*2A 1
For Europe
E3101027 FU Fuse 10*38*20A 3
For Europe
E2305002
Pilot Light YK∅∅∅∅22 24V(W) 1
Optional
E1602001 Safety Switch XF 163B 1
Optional
Page 84
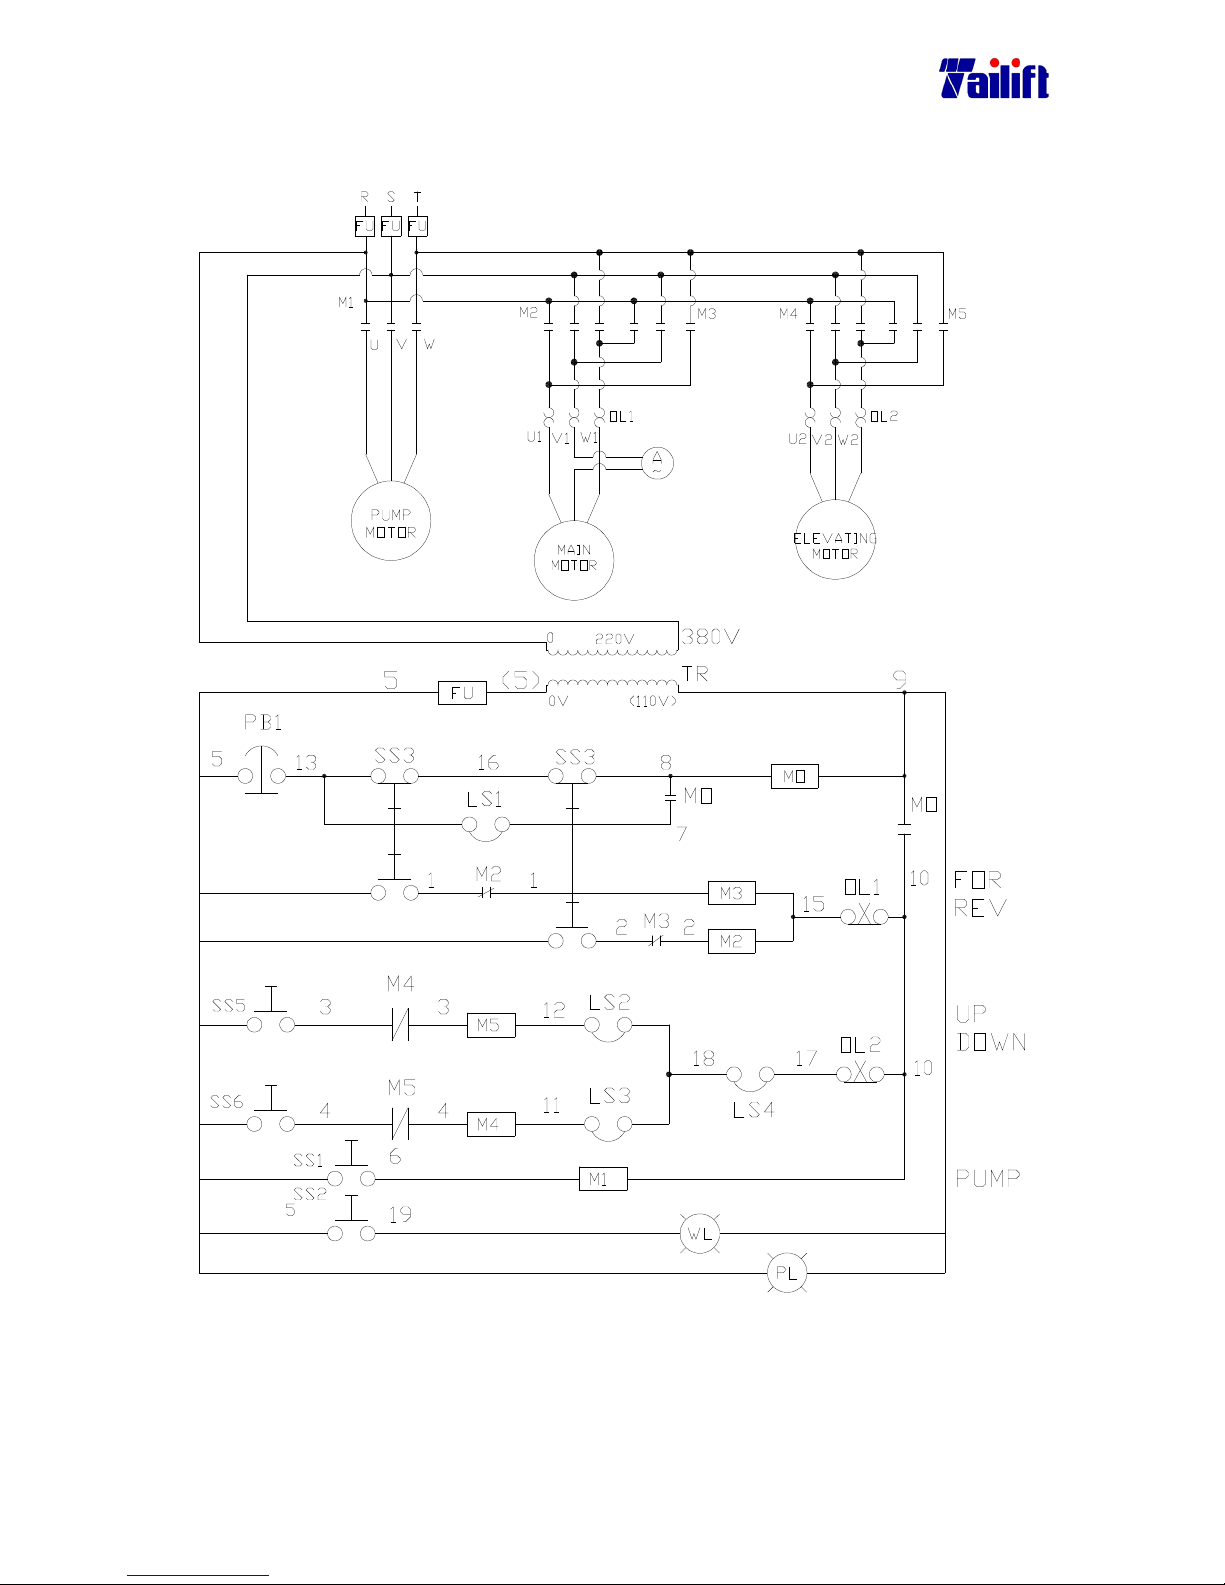
9-9
9.8 Electrical Circuit Diagram
(For TPR1100 Standard)
Page 85
9-10
9.9 Eletrical main parts list
(For TPR1100 Standard )
Part NO. Symbol
Name Specification Q’ty
Remark
E0701006 M1 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M4 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M5 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701006 M0 Magnetic Contact CN11 3a1b 110V 1 Standard
E0701007 M2 Magnetic Contact CN18 110V 1 Standard
E0701007 M3 Magnetic Contact CN18 110V 1 Standard
E3101009
FU Fuse Seat E-16 4
For Asia
E3101010
FU Fuse E 16 30A 3
For Asia
E3101013
FU Fuse E 16 6A 1
For Asia
E1801005 TR Transformer PT40 1 Standard
E0207010
OL1 Overload Relay RH 18/15 1
For 200V~230V
E0207011
OL1 Overload Relay RH 18/7 1
For 380V~460V
E0207007
OL2 Overload Relay RH 18/4 1
For 220V~230V
E0207008
OL2 Overload Relay RH 18/1.7 1
For 380V~460V
E1618001
PB1 Emg.Push Button
Switch
SBT-307 1
Standard
E1303001
SS1 Selector Switch ST 302 1
Standard
E1604001
SS2 Selector Switch SN1021 1
Standard
E1605001
SS3 Cross Switch
3 Joint UP1A Down1A
Left1A1B Right1A1B
1
Option
E0901021 SS3 Limit Switch V-15-1E5 4 Standard
E1603001
SS4 Pole Reversing
Switch
A441 CA10 1
Standard
B100006
SS5 Push button ZB4-BA2+ZB4-BZ101 1
Standard
B100006
SS6 Push button ZB4-BA2+ZB4-BZ101 1
Standard
E0901006
LS1 Limit Switch MJ2-1308R 1
Standard
E0901014
LS2 Limit Switch MJ2-1308 1 Standard
E0901014
LS3 Limit Switch MJ2-1308 1 Standard
E0901034
LS4 Limit Switch AZ 7311 1 Standard
E1701002
WL Work Lamp FS51441 1 Standard
E2303003
PL Pilot Light SP-301 110V(R) 1 Standard
E2303004
PL Pilot Light SP-301 110V(W) 1 Standard
E3602001
Amp Meter S065 30A 1
For 200V~230V
E3602002
Amp Meter S065 20A 1
For 380V~460V
Page 86
9-11
Part NO. Symbol
Name Specification Q’ty
Remark
Coolant Pump
Motor
1/8HP/2P/3PH
L:130mm
1
Standard
Main Motor Vertical
3HP/1.5HP4P/8P
1
Standard
Elevating Motor Horizontal
1HP/4P/3PH
1
Standard
E0703001 M1 Magnetic Contact CN11 3a1b 24V 1 Optional
E0703001 M4 Magnetic Contact CN11 3a1b 24V 1 Optional
E0703001 M5 Magnetic Contact CN11 3a1b 24V 1 Optional
E0703001 M0 Magnetic Contact CN11 3a1b 24V 1 Optional
E0703002 M2 Magnetic Contact CN18 24V 1 Optional
E0703002 M3 Magnetic Contact CN18 24V 1 Optional
E2802003 FU Fuse Seat 3P(14*51) 1 For U.S.A
E2802013 FU Fuse Seat 1P(14*51) 1 For U.S.A
E3101016 FU Fuse 5A(14*51) 1 For U.S.A
E3101012 FU Fuse 40A(14*51) 3 For U.S.A
E3101019
FU Fuse Seat 10*38 4
For Europe
E3101022
FU Fuse 10*38 2A 1
For Europe
E3101027 FU Fuse 10*38 20A 3 For Europe
E2305003
Pilot Light
YK30ΦΦΦΦ 24V(R)
1
Optional
E2305001
Pilot Light
YK30ΦΦΦΦ 24V(W)
1
Optional
E1602001 Safety Switch XF 163B 1
Optional
E1801005 TR Transformer PT40 1
Standard
 Loading...