

Page 1
Operating Instructions
BMS-6 ISO
Stud Welder
Page 2
BMS-6 ISO
2
Page 3
BMS-6 ISO
Operating Instructions
BMS-6 ISO
Stud Welder
Serial number*
BMS-6 ISO stud welder _________________________
Please enter the serial number here, so that the data is
immediately available if you need service support.
Heinz Soyer Bolzenschweißtechnik GmbH
Etterschlag
Inninger Straße 14
82237 Wörthsee
Telephone +49 (0) 8153 - 885 - 0
Telefax +49 (0) 8153 – 8030
www.soyer.de
3
Page 4
BMS-6 ISO
We congratulate you on purchasing the BMS-6 ISO SOYER stud welder.
You have made an excellent choice. Your BMS-6 ISO SOYER stud welder was
especially developed for high-speed fastening of insulating nails, cupped head pins and
SOYER welding studs in compliance with DIN EN ISO 13 918 on metallic workpieces .
SOYER® is a registered trade mark of Heinz Soyer Bolzenschweißtechnik GmbH.
It is prohibited to transmit or reprint this document, as well as to utilize or disclose its
contents, unless this has been expressly granted.
Non-compliance with this regulation is liable to compensation. All rights reserved,
particularly in the case of a patent grant or a GM registration.
We have verified that the contents of this pamphlet correspond to the hard- and
software described. Deviations, however, cannot be excluded so that we cannot
warrant for absolute compliance.
The data in this documentation, however, have been verified regularly and necessary
corrections will be incorporated in future impressions. We appreciate any suggestions
for improvement.
Date of issue: April 01, 2002
© Heinz Soyer Bolzenschweißtechnik GmbH 2002 · All rights reserved
Printed in the Federal Republic of Germany
4
Page 5
BMS-6 ISO
Heinz Soyer Bolzenschweißtechnik GmbH
Inninger Straße 14
82237 Wörthsee
CE Declaration of Conformity
We herewith declare that the machine described in the following and the version available on the
market correspond in design and construction to the safety and health requirements of the listed
guidelines and standards. Any unauthorised modification to this machine automatically annuls this
declaration.
Designation of machine : Stud welding device
Machine type : BMS-6 ISO
Machine no. : ______________________
Applicable EU directives : RoHS Directive (2011/65/EU)
Low Voltage Directive (2014/35/EU)
EMC Directive (2014/30/EU)
Applied harmonised : EN 60 974-1:2012
standards, in particular EN 60 974-10:2008
Applied national standards : DGUV Regulation 1
Date : 16 July 2015
Producer’s signature : ____________________
Signer’s function : Managing Director
5
Page 6
BMS-6 ISO
Table of contents
1 General ........................................................................................................................................... 9
1.1 The following should be principally observed... ..................................................................... 9
1.2 Application ............................................................................................................................ 10
1.3 Information on the product ................................................................................................... 10
1.4 Type plate............................................................................................................................. 10
1.5 Information on the documentation ....................................................................................... 10
1.5.1 Chapters of operating instructions ................................................................................... 11
1.5.2 Information on operating instructions .............................................................................. 11
1.5.3 Conduct in the case of malfunctions ................................................................................ 12
1.6 Contacts and service address .............................................................................................. 12
2 Description of stud welder ......................................................................................................... 13
2.1 Description of technology ..................................................................................................... 13
2.2 Stud welder set-up ............................................................................................................... 13
2.3 View ...................................................................................................................................... 14
2.4 Technical data ...................................................................................................................... 15
2.5 Circuit diagram of BMS-6 ISO .............................................................................................. 16
2.6 Alteration of mains voltage to 115 / 230 volt ........................................................................ 16
3 Safety instructions...................................................................................................................... 17
3.1 Description of reference signs in the operating instructions ................................................ 17
3.2 Staff qualification and training .............................................................................................. 17
3.3 Dangers in the case of non-compliance with safety instructions ......................................... 18
3.4 Safety-conscious working .................................................................................................... 18
3.5 Safety instructions for the operator/user .............................................................................. 18
3.6 The following should be observed before starting the system… ......................................... 18
3.7 Before starting to weld ... ..................................................................................................... 19
3.8 Safety precautions at installation site ................................................................................... 19
3.9 Working with the stud welding equipment ............................................................................ 19
3.10 Safety instructions for maintenance, inspection and assembly works ................................. 20
3.11 Unauthorized retrofit and spare parts production ................................................................ 20
3.12 Inadmissible operating methods .......................................................................................... 20
3.13 Stopping the stud welder ...................................................................................................... 20
3.14 The “S” symbol ..................................................................................................................... 21
4 Installation of stud welder ......................................................................................................... 22
5 Start-up ........................................................................................................................................ 23
5.1 Total view ............................................................................................................................. 23
6
Page 7
BMS-6 ISO
5.1.1 Operating elements ......................................................................................................... 23
5.1.2 Display elements ............................................................................................................. 24
5.1.3 Connecting elements ....................................................................................................... 24
5.1.4 Symbols ........................................................................................................................... 24
5.1.5 Fuse elements ................................................................................................................. 24
5.2 Preparation for start-up ........................................................................................................ 25
5.2.1 Earth connection .............................................................................................................. 25
5.2.2 Connection of stud welding gun....................................................................................... 25
5.2.3 Mains supply .................................................................................................................... 25
5.3 Operation.............................................................................................................................. 26
5.4 Welding parameters ............................................................................................................. 27
6 Quality control ............................................................................................................................. 28
6.1 General ................................................................................................................................. 28
6.2 Demands on the company ................................................................................................... 28
6.3 Proof of qualification ............................................................................................................. 28
6.4 Type and scope of test ......................................................................................................... 28
6.4.1 Standard work test ........................................................................................................... 28
6.4.2 Simplified work test .......................................................................................................... 29
6.5 Test execution ...................................................................................................................... 29
6.5.1 Production of samples ..................................................................................................... 29
6.5.2 Visual inspection .............................................................................................................. 29
6.5.3 Tensile test ....................................................................................................................... 29
6.5.4 Bend test .......................................................................................................................... 29
7 Maintenance ................................................................................................................................ 30
7.1 Stud welder .......................................................................................................................... 30
7.2 Cleaning ............................................................................................................................... 30
7.2.1 Detergents ....................................................................................................................... 30
7.3 Replacement of components ............................................................................................... 30
7.4 Fuses .................................................................................................................................... 30
8 Spare parts for BMS-6 ISO ......................................................................................................... 32
8.1 Spare parts for BMS-6 ISO .................................................................................................. 32
9 Troubleshooting .......................................................................................................................... 33
9.1 Error code overview ............................................................................................................. 34
9.2 Troubleshooting ................................................................................................................... 35
10 Transport and storage ................................................................................................................ 37
11 Terms of warranty ....................................................................................................................... 37
12 Standards and guidelines .......................................................................................................... 38
7
Page 8
BMS-6 ISO
Appendix A / PS-1 and PS-1K – Capacitor discharge
Adjustment of PS-1 and PS-1K stud welding guns Appendix A
Appendix B / PS-1KI – Capacitor discharge
Adjustment of PS-1KI stud welding gun Appendix B
8
Page 9
BMS-6 ISO
1 General
1.1 The following should be principally observed...
With this stud welder you have purchased a product which
• is state-of-the-art technology
• fully complies with the current safety requirements and
• enables successful working.
Before installing the stud welder, please observe the following:
• Store the operating instructions in a place accessible to every operator
• Ensure that the respective operator has read and understood the operating
instructions prior to installation. Each operator should confirm this per
signature.
• Prevent the stud welder being operated by unauthorized personnel
• Only trained personnel may operate the stud welder
MORTAL DANGER
Persons with pacemakers must not operate the stud welding equipment and
must not stay near it while it is running. Ensure that the stud welding
equipment is not operated near electronically sensitive life-supporting
equipment, such as in intensive care units in hospitals.
WARNING
Keep sufficient distance from electronic devices. When stud welding, highly
intensive electromagnetic fields are created which may permanently damage
these devices (e.g. television sets).
• Moreover, please observe the safety instructions in chapter 3.
• Call a doctor in case of an accident.
9
Page 10
BMS-6 ISO
1.2 Application
The BMS-6 ISO SOYER ® stud welder with capacitor discharge allows you to
weld SOYER threaded studs, nails and pins with flange in compliance with
DIN EN ISO 13918 and ranging from M3 - M6 or Ø 2 - 5.5 mm made of
coppered steel, stainless steel, brass and aluminium as well as steel cupped
head pins from 2 - 2.7 mm diameter. No auxiliary aids such as shielding gas,
ceramic ferrules or soldering materials are required.
There is usually no reverse marking, discoloration or deformation of the sheet,
so that even thin sheet metals with a thickness of below 1 mm retain their
decorative appearance.
If you need consultation or assistance in solving problems, please contact
either our parent company or our field engineers.
1.3 Information on the product
Manufacturer Heinz Soyer Bolzenschweißtechnik GmbH
Etterschlag
Inninger Straße 14
D-82237 Wörthsee
Telephone +49 (0) 8153-885-0
Telefax +49 (0) 8153-8030
Product designation BMS-6 ISO stud welder
Country of origin Germany
1.4 Type plate
The type plate is located on the rear side of the stud welder. It contains the following
information:
• Manufacturer’s name
• Manufacturer’s address
• Country of origin
• Product designation
• Date of construction
• Production number
• Performance data
• Mains connection values
1.5 Information on the documentation
The following operating instructions are supplied with the BMS-6 ISO stud welder:
• Operating instructions for BMS-6 ISO
Order no.: P00252
For repeat-orders please contact your responsible service office or our parent
company. Please refer to chapter 1.6.
10
Page 11
BMS-6 ISO
1.5.1 Chapters of operating instructions
The operating instructions describe the start-up and operation of the BMS-6 ISO stud
welder under normal conditions.
The present operating instructions of the BMS-6 ISO stud welder comprise the
following chapters in detail:
• Chapter 1 "General".
Information on application and product, as well as supplementary information.
• Chapter 2 "Description of stud welder". Description of technology.
• Chapter 3" Safety instructions". All safety regulations which are relevant with regard
to installation and operation of the stud welding system.
• Chapter 4 "Installation of stud welder".
• Chapter 5 "Start-up".
• Chapter 6 "Quality control".
• Chapter 7 "Maintenance". Maintenance measures.
• Chapter 8 "Spare parts"
• Chapter 9 "Troubleshooting”.
• Chapter 10 "Transport and storage".
• Chapter 11 "Terms of warranty".
• Chapter 12 "Standards and guidelines".
1.5.2 Information on operating instructions
Legal relationship
We draw your attention to the fact that the contents of these operating instructions are
neither part of any former or existing arrangement, pledge or legal relationship nor are
designed for modifying the latter. All obligations of Heinz Soyer Bolzenschweißtechnik
GmbH result from the respective contract of purchase which also comprises the
complete and generally valid warranties. These contractual warranty terms are neither
extended nor restricted by the implementation of these operating instructions.
WARNING
Do not carry out any actions on the stud welding system without specifically knowing
the operating instructions or the respective part. Ensure that only qualified personnel
familiar with the operating instructions and the necessary technical activities (training!)
operate the system.
11
Page 12
BMS-6 ISO
1.5.3 Conduct in the case of malfunctions
If malfunctions occur, first try to detect and eliminate the causes according to the list in
chapter 9 "Troubleshooting" of our operating instructions. In all other cases, contact
our service department.
If you require our service, please make sure that you supply us with the following
information:
•Customer number
•Product designation
•Serial number
•Year of construction
•Options
•Material of stud and workpiece
•Stud diameters
This information will help us both to save time and unnecessary costs, e.g. caused by
delivering the wrong spare parts.
1.6 Contacts and service address
If you have any questions regarding the operation of the stud welding system, retrofits
or if you require service, please contact your responsible service office or the following
address:
Heinz Soyer Bolzenschweißtechnik GmbH
Etterschlag
Inninger Straße 14
D-82237 Wörthsee
Telephone +49 (0) 8153-885-0
Telefax +49 (0) 8153-8030
[email protected]
www.soyer.de
12
Page 13
BMS-6 ISO
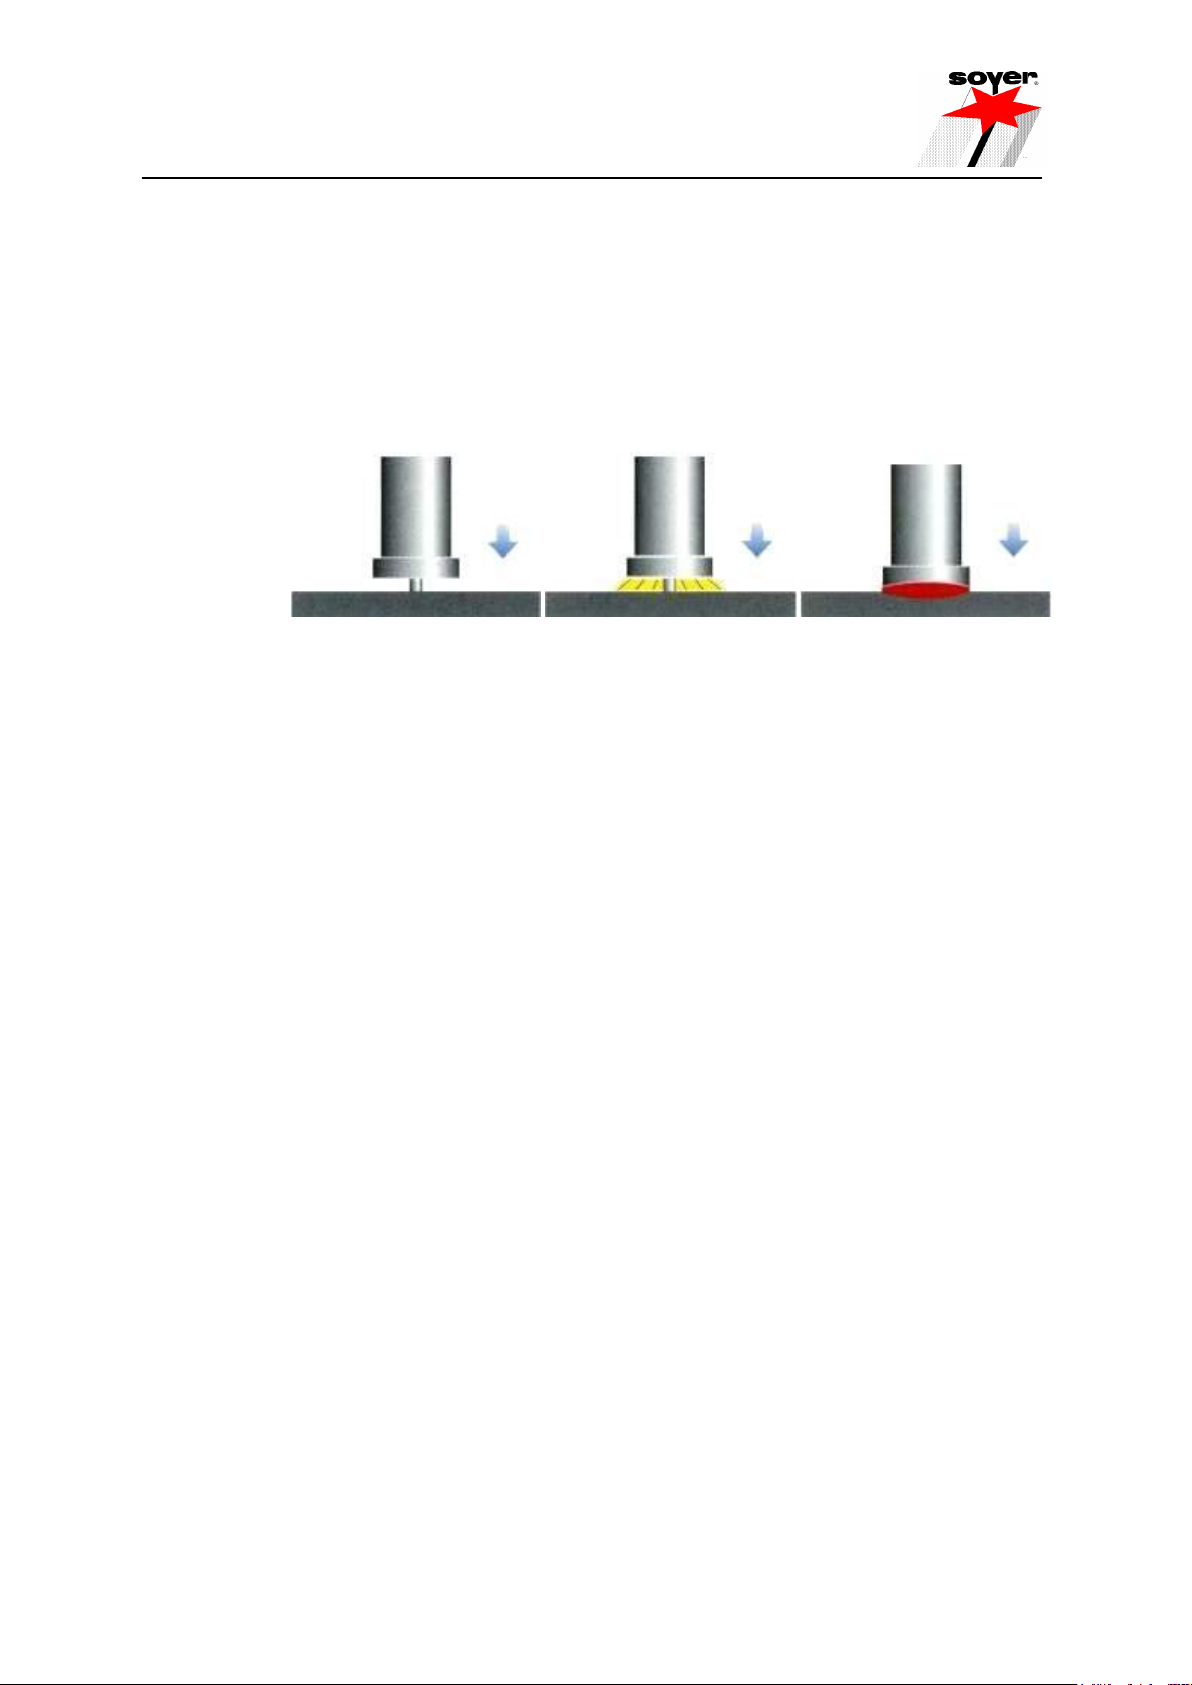
Stud tip touches
workpiece. Electric arc is
initiated.
Ignited arc generates a
thin fusion zone on stud
and workpiece.
Stud is plunged in molten
pool. Material solidifies
and stud is welded.
2 Description of stud welder
2.1 Description of technology
BMS-6 ISO SOYER stud welding systems function according to the principle of
capacitor discharge (TS) in compliance with DIN EN ISO 14555 and as defined in
DVS information sheet 0903 (German Welding Society).
This system takes advantage of the sudden discharge of a capacitor battery to
generate electric arc energy.
The electric arc is initiated via the calibrated and close-fit ignition tip of the welding
studs and welding elements. The stud weld base and the opposite surface of the
workpiece thus start to melt. The stud is then automatically dipped into the thin fusion
zone or into the liquid weld pool. After immediate solidification of the material, an
homogenous high-strength joint is produced in an extremely short welding time of only
1 – 3 milliseconds (0.001 – 0.003 sec.).
2.2 Stud welder set-up
The standard gun to be connected to the BMS-6 ISO stud welder is the PS-1 stud
welding gun with control cable and support tube.
Optionally it is possible to connect the PS-1KI stud welding gun for cupped head pins
or the PS-3K, PS-0K, PS-1K contact guns for studs and insulating nails with ignition
tip to the stud welder. These operating instructions only refer to the BMS-6 ISO stud
welder.
For information regarding the stud welding guns required and their adjustment, please
refer to the relevant operating instructions of the stud welding guns.
13
Page 14
2.3 View
BMS-6 ISO
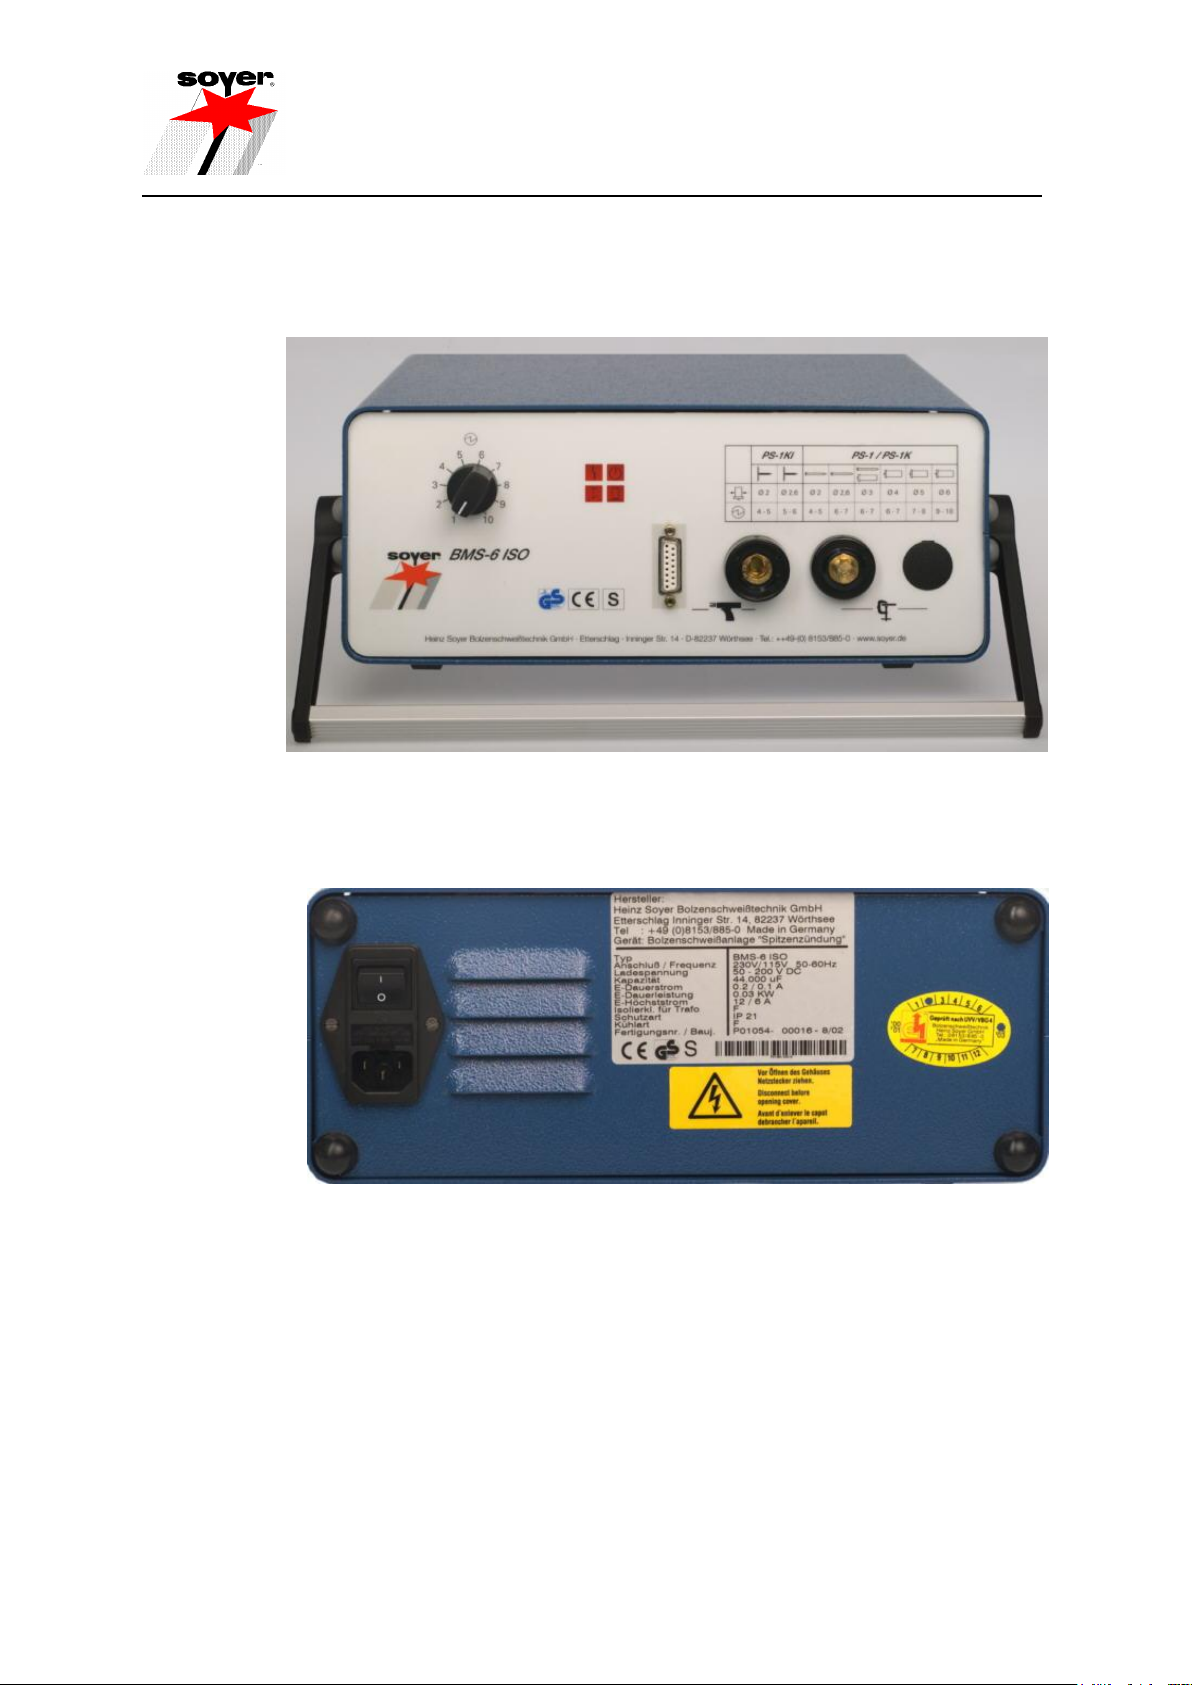
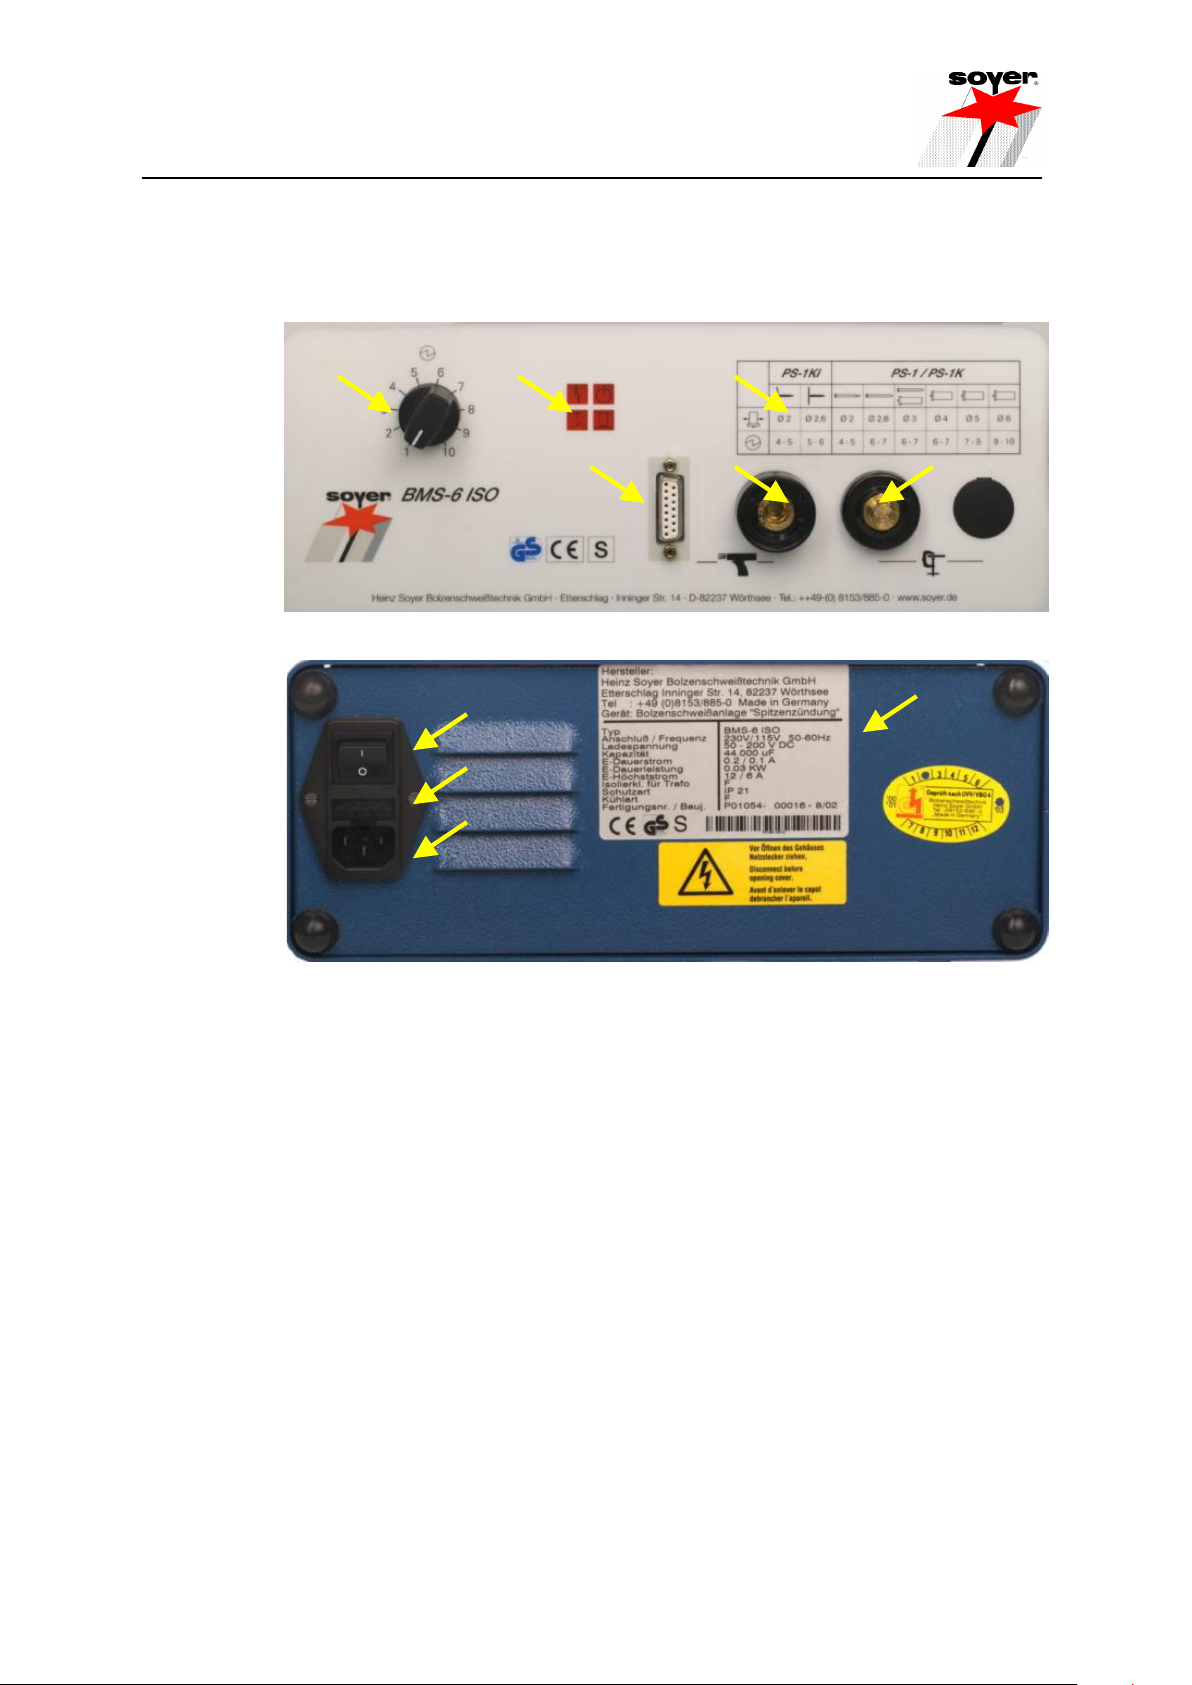
The BMS-6 ISO stud welder has a handy, compact and robust design. It has a
carrying handle and can be optionally equipped with a shoulder strap.
Illustration: Front view of BMS-6ISO
Dimensions 300 x 120 x 320 mm (w x h x d)
Illustration: Rear view of BMS-6ISO
14
Page 15
BMS-6 ISO
Designation
BMS-6 ISO
Welding range
SOYER threaded flanged studs, nails and pins as per DIN
EN ISO 13918 from M3 – M6 or 2 – 5.5 mm dia, as well as
cupped head pins from 2 –2.7 mm dia and 10 – 55 mm in
length
Material
Steel, stainless steel, aluminium and brass
Welding process
Capacitor discharge according to DIN EN ISO 14555 and
DVS information sheet 0903
Standard gun
PS-1 stud welding gun with support tube
Power source
Capacitor battery
Charging capacity
44,000 μF
Charging voltage
50 – 200 volt infinitely variable
Welding time
0.001 – 0.003 sec
Welding sequence
up to 20 nails or studs / min., depending on stud diameter
Mains supply
115 / 230 Vz shock-proof socket
Operation with 115 V
reclamping works in the control device
Fuse element
G - fuse link 5 x 20 mm, 2 x 10 A slow, 250 V.
The fuse links are integrated in the cold mounting plug at the
rear side of the stud welder
Weight*
8.4 kg (stud welder without cable)
Colour
RAL 5009 azure blue
Subject to technical changes
2.4 Technical data
*Slight deviations are possible depending on accessories.
15
Page 16
BMS-6 ISO
Toroidal mains transformer
+
+
KL8
KL9
KL10
KL11
KL12
KL13
KL14
KL15
KL16
KL17
KL18
KL19
KL20
KL21
KL1
KL2
KL3
KL4
KL5
KL6
KL7
10AT
10AT
PE
N
Mains supply
115/230Vac
50/60Hz
22R
22mF
22mF
3R9
K275
SO105 ISO
26-pole
Front panel PC Board
Machine PC Board
L1
I/0
Core 20
5 turns
white
yellow
green
brown
black
brown
yellow / green
red
red
blue
blue
blue
red
white
blue
brown
brown
grey
Discharging
resistor
red
red
blue
blue
black
white
yellow
green
# BV 973 701.3
Core 25
4 turns
Core 20
5 turns
+ EARTH
+ EARTH
- PISTOL
safety resistor
190V
20V
Cathode
Gate
100W
rt
100W
115V
115V
Flat cable
15-pole socket
1
9
Trigger
Pistol
F1 6.3AT
charging circuit
F2 1A
F3 250mA
control circuit
ventilator
130°C
S30E4A
Charging
module
red
bl
bl
1000µF
2200µF
+ +
-
-
Measuring points
5Vdc
26Vdc
SO115Rev.3
F6 230V
F5 230V
F4 115V
F7 115V
F1 6.3AT
Steuerplatine SO-115 Rev. 3 (SMD)
Control printed circuit SO-115 Rev. 3
F3 250mA
F2 1AT
F4 10AT
F7 10AT
Steuerplatine SO-115 Rev. 3 (SMD)
Control printed circuit SO-115 Rev. 3
F1 6.3AT
F3 250mA
F2 1AT
F5 10AT
F6 10AT
F4 115 V
F7 115 V
F5 230 V
F6 230 V
Netzspannung / Line voltage 115 Volt AC
Sicherung 10AT in Sicherungshalter F4 und F7 einsetzen.
Netzspannung / Line voltage 230 Volt AC
Sicherung 10AT in Sicherungshalter F5 und F6 einsetzen.
setting 115V AC setting 230V AC
Insert fuse 10AT into F4 and F7 fuse holders
Insert fuse 10AT into F5 and F6 fuse holders
No. F04538/FA
No. F04538/FA
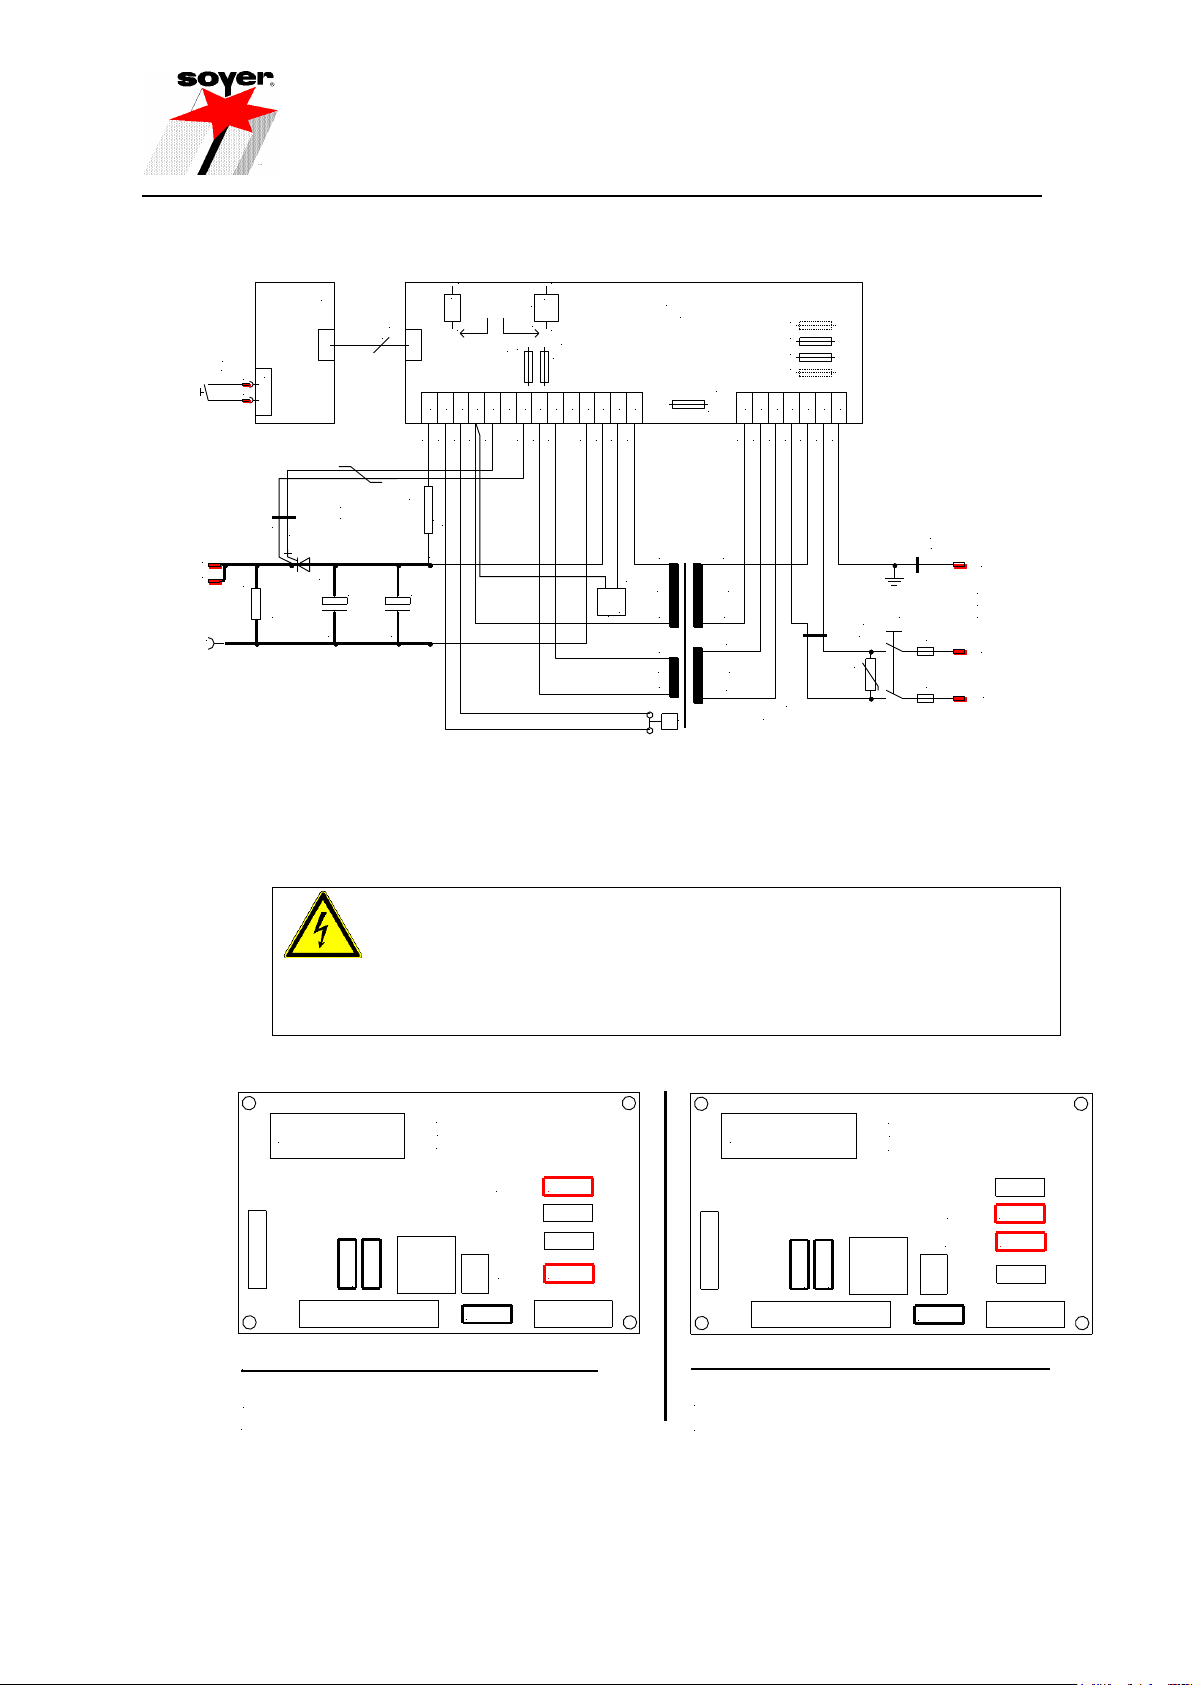
2.5 Circuit diagram of BMS-6 ISO
Subject to technical changes
2.6 Alteration of mains voltage to 115 / 230 volt
Always disconnect the connecting plug from the mains supply socket before opening
the housing of the stud welding equipment. Only trained and appropriately qualified
personnel are allowed to carry out works on the electric power supply and stud welder.
16
MORTAL DANGER
Page 17
BMS-6 ISO
3 Safety instructions
These operating instructions contain basic instructions which have to be complied with
during installation or operation. It is therefore absolutely necessary that these
operating instructions are read by the operator and responsible specialist staff prior to
assembly and start-up. The operating instructions must always be available at the
installation site.
Not only the general “safety instructions” listed under this main item, but also the
special safety instructions e.g. for high temperatures, voltage etc. listed under the
other main items have to be complied with.
3.1 Description of reference signs in the operating instructions
The non-observance of safety instructions can cause damage to persons. The safety
instructions of this manual are marked with the general symbol for danger
safety symbol in compliance with DIN 4844 - W9
Warning of electric voltage is specially marked with the
safety symbol in compliance with DIN 4844 - W8.
In addition to these symbols, the terms "DANGER TO HEALTH" or "MORTAL
DANGER" refer to the degree of a possible danger.
Safety instructions, the non-observance of which may endanger the machine and its
functions, are marked with the words "CAUTION " or "WARNING".
General instructions are marked with the hand symbol
3.2 Staff qualification and training
The staff responsible for operation, maintenance, inspection and assembly must have
the respective qualification for carrying out these works. Field of responsibility,
competence and the supervision of staff has to be exactly regulated by the user. If
your personnel do not have the necessary knowledge, they have to be trained and
instructed. If necessary, this can be done by the manufacturer/supplier on behalf of
the user. Furthermore, the user must ensure that the contents of the operating
instructions are fully understood by the staff.
The society of welding institutes (GSI: Gesellschaft der Schweißtechnischen Institute
mbH) offers the appropriate training courses for your personnel.
For information on branches, please refer to website http://www.dvs-ev.de.
17
Page 18
BMS-6 ISO
3.3 Dangers in the case of non-compliance with safety instructions
The non-compliance with safety instructions may not only endanger persons, but also
the welding equipment and its environment. Any non-compliance with safety
instructions may result in a complete loss of damage claims.
Non-compliance with safety instructions may have the following consequences:
• Failure of important system functions
• Failure of prescribed methods for maintenance
• Danger of persons through electric, mechanic, thermal and acoustic influences
3.4 Safety-conscious working
The safety instructions listed in this manual, existing national accident prevention
regulations and possible international working, operating and safety regulations of the
user must be complied with.
3.5 Safety instructions for the operator/user
When stud welding, danger may result from
• electric current
• optical radiation
• harmful substances (smoke)
• acoustic shock
• spraying sparks
Your are therefore obliged to restrict dangers to an inevitable degree and to point
these dangers out to the operator and other persons involved.
MORTAL DANGER
Persons with pacemakers must neither operate the stud welder nor stay near it.
3.6 The following should be observed before starting the system…
Before starting up the system, pay attention to the following information:
• Juveniles under the age of 16 years must not operate the stud welding system.
• Read all of the operating instructions before starting the system.
• Only qualified personnel are allowed to operate the system.
• Prevent unauthorized use of the system by children or unqualified personnel.
•.Wear non-combustible closed working clothes.
• Wear a leather apron to protect your clothes from welding spatters that are
generated during the welding process.
• Wear a head protection when carrying out welding works above your head.
MORTAL DANGER
When welding, do not wear clothes soiled with easily combustible substances such as
oil, grease and paraffin oil etc.
• Wear gauntlet gloves made of leather.
• Wear neither rings, watches nor electrically conductive jewellery.
18
Page 19
BMS-6 ISO
• Wear protective goggles with eye-protecting lens number 2 (DIN 58211, part 6) to
protect your eyes from welding spatters and flashes of light that are generated during
the welding process.
• Wear side-shielded glasses.
• Wear ear protection. Capacitor discharge generates a loud bang.
3.7 Before starting to weld ...
• Check the state of all cables and cable connections before starting to weld.
• Immediately replace defective cables and cable connections.
• Ensure that the air apertures of the housing are not covered. Heat accumulation may
damage the stud welding device.
3.8 Safety precautions at installation site
• When placing the stud welder on tables or similar workshop furniture, ensure that the
system stands firmly and that the table can bear its weight.
• Make sure mains socket and stud welding system are properly earthed.
• Comply with fire prevention regulations and do not weld in hazardous locations.
• Make sure room is well ventilated or extract welding fumes, if necessary.
DANGER TO HEALTH
When welding, fumes and suspended matters may be generated. Beware of fumes
detrimental to health, particularly when using surface-treated materials. If possible,
only weld in rooms which are higher than 3 m. As per VBG 15 special regulations
apply to narrow rooms.
3.9 Working with the stud welding equipment
• Comply with all accident prevention regulations which apply to the operation of your
stud welding device.
One of the accident prevention regulations applicable to stud welders is VGB15
“Welding, cutting and similar working methods”. For more information, please contact
the Employer’s Liability Insurance Association.
MORTAL DANGER
When welding, do not wear clothes soiled with easily combustible substances such as
oil, grease and paraffin oil etc.
19
Page 20
BMS-6 ISO
MORTAL DANGER
Persons with pacemakers must neither operate the stud welder nor stay near it.
If an accident happens,
• switch off the welding device and disconnect it from the mains supply
• call a doctor.
3.10 Safety instructions for maintenance, inspection and assembly works
Only carry out maintenance works when the welding equipment has been switched off
The user must ensure that all maintenance, inspection and assembly works are only
carried out by authorized and qualified technical personnel.
Generally, only work at the system when it has been switched off and after having
disconnected it from the mains supply. The safety instructions described in the
operating instructions have to be complied with.
Immediately after having completed your work, re-install and activate all safety and
protective devices.
3.11 Unauthorized retrofit and spare parts production
The system may only be retrofitted and modified after consultation with the
manufacturer. Original spare parts and accessories authorized by the manufacturer
guarantee safety. The use of other parts may result in the cancellation of warranty for
any consequences thus caused.
3.12 Inadmissible operating methods
Limit values
Working safety of the stud welding system supplied can only be guaranteed if the
system is used in accordance with its purpose. The limit values indicated in the
chapter “Technical data” must never be exceeded.
3.13 Stopping the stud welder
• Switch off the mains switch (item 7, chapter 5.1) at the rear side of the stud welder
• Disconnect the mains plug from the socket.
• Disconnect
- the control cable (item 4, chapter 5.1)
- the welding cable (item 5, chapter 5.1)
- the earth cable (item 6, chapter 5.1)
from the stud welder.
• Roll up the cables without buckling them.
20
Page 21
BMS-6 ISO
Our GK-2 SOYER suitcase (optional equipment) is the optimum solution for properly
storing SOYER stud welders as well as welding guns, cables, studs, retrofit kits etc.
• Make sure stud welder can not be used by unauthorized persons.
• Check welding cable and connections of the stud welder for damage such as burn-
off, mechanical wear etc. and have damaged parts replaced by the SOYER
customer service.
3.14 The “S” symbol
MORTAL DANGER
The “S” symbol is the symbol for welding current sources permitted for operation with
increased electrical danger. The “S” symbol on our stud welders refers exclusively to
the welding current circuit and not to the complete stud welder.
21
Page 22
BMS-6 ISO
4 Installation of stud welder
• Only install the stud welder on an even surface. The four anti-vibration pads located
on the bottom of the system guarantee its anti-skid position.
• Although the stud welder is resistant to environmental influences, it should be
protected against dampness and dust. This is easily achieved by installing the
system on a workbench.
• Please pay particular attention to the bearing strength of the workshop furniture and
a safe and stable position.
• Install the stud welder close to the welding location.
• Please consider that additional extension cables cause a voltage drop which might
lead to disturbances in the stud welder.
The housing of the BMS-6 ISO stud welder corresponds to safety class IP 21. Please
observe that this system of protection is not suitable for being operated or transported
in the rain.
22
Page 23
BMS-6 ISO
1 2 3
4 5 6
7 10
8
9
5 Start-up
5.1 Total view
1 Potentiometer for charging voltage 6 Earth cable connector
2 Light-emitting diodes for function control 7 Mains switch
3 Table indicating welding parameters 8 Fuses
4 Control cable connection 9 Mains connection
5 Welding cable socket 10 Type plate
5.1.1 Operating elements
• Potentiometer (item 1, chapter 5.1)
The potentiometer enables the continuous adjustment of the charging voltage.
• Mains switch (item 7, chapter 5.1)
The mains switch located at the rear of the stud welder serves to switch the stud
welder on and off.
23
Page 24
BMS-6 ISO
4.1 LED
"Malfunction"
4.3 LED "Release”
4.2 LED "Ready"
4.4 LED "Stud on
Workpiece”
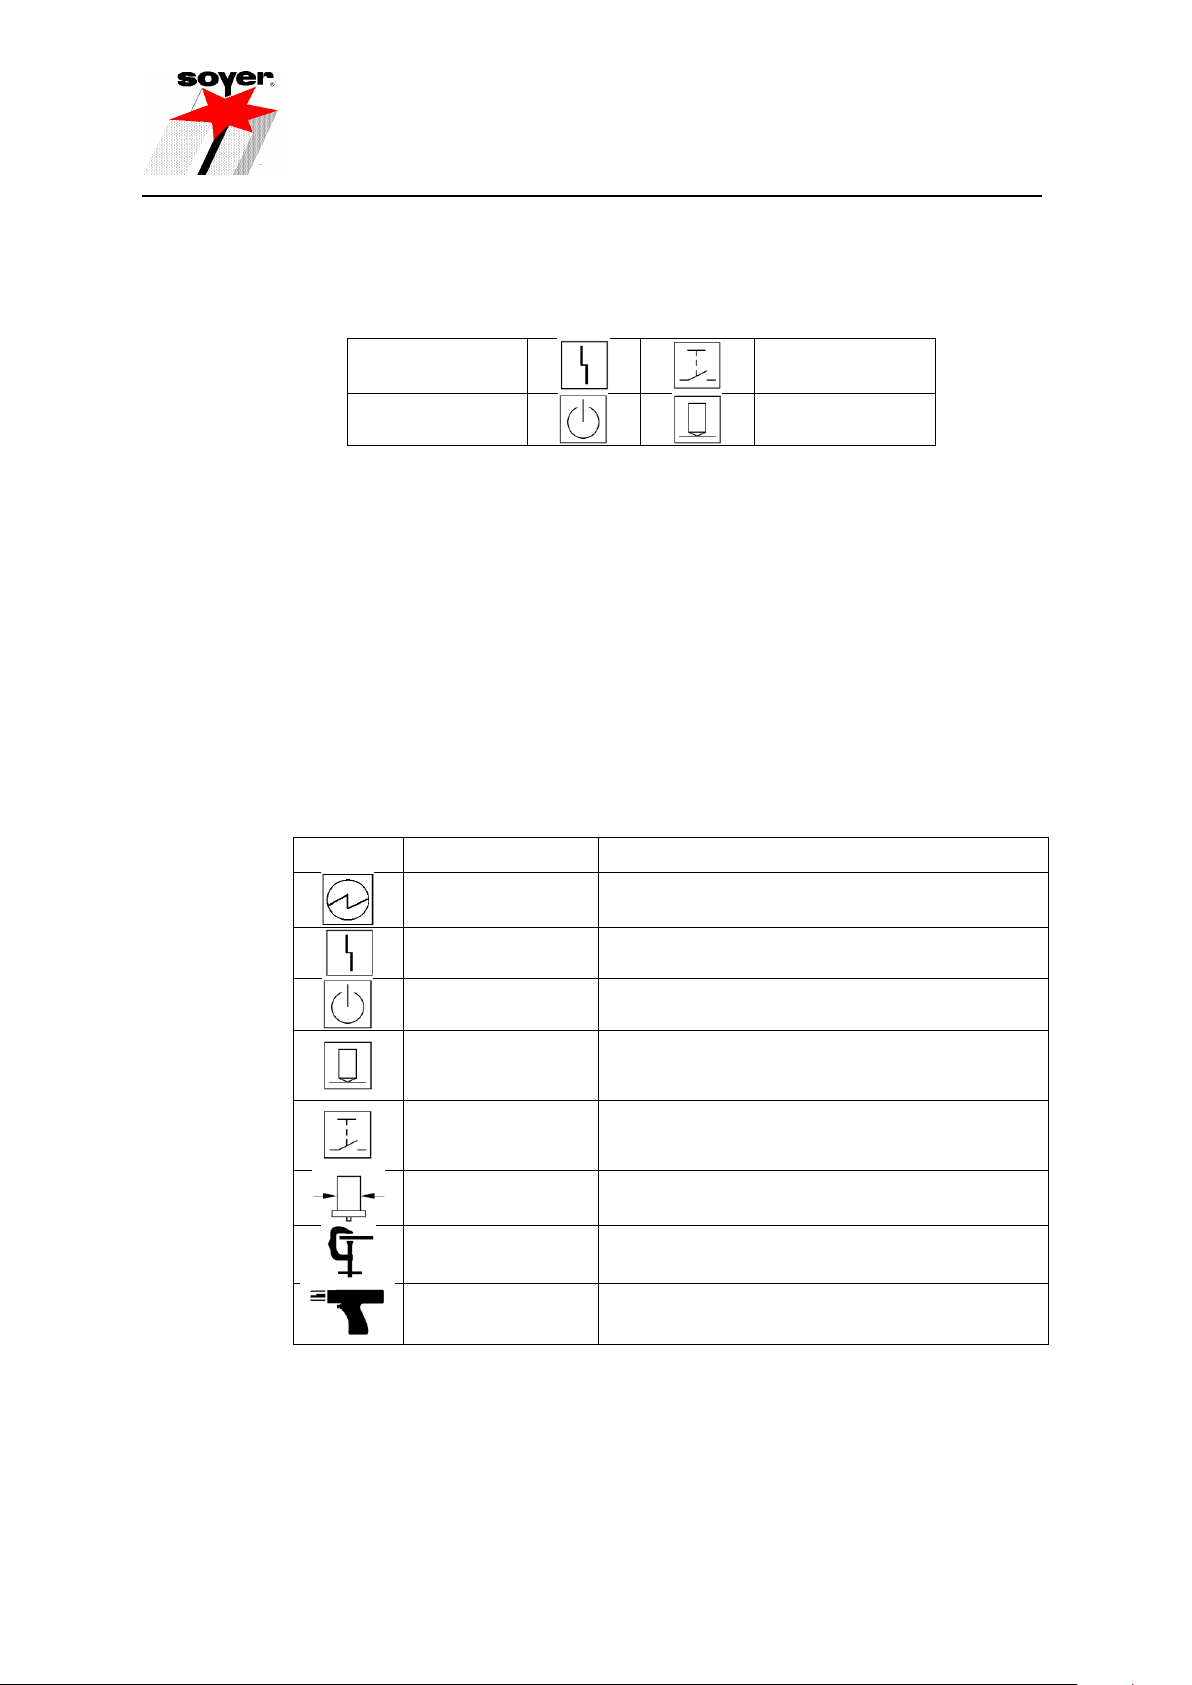
Symbol
Designation
Function
Potentiometer
Infinitely variable adjustment of charging voltage
LED “Malfunction“
LED lights up when stud welder fails
LED "Ready"
LED lights up when stud welder is ready for
operation
LED "Stud on
Workpiece”
LED lights up when earth terminal is connected
and stud touches the workpiece
LED
"Release"
LED lights up when trigger switch on welding
gun or welding head is pressed
Stud diameter
Symbol of stud diameter
Ground
Symbol of earth cable connector for connecting
the earth cable
Gun
Symbol of control cable and welding cable
sockets for connecting the gun
5.1.2 Display elements
• LED displays (item 2, chapter 5.1)
The LED displays show the respective operational states.
5.1.3 Connecting elements
• Control cable socket (item 4, chapter 5.1) and welding cable socket (item 5,
chapter 5.1)
The control cable connection and welding cable socket serve to connect the stud
welding gun to the stud welder .
• Earth cable connector (item 6, chapter 5.1)
The earth cable connector serves to connect the earth terminals to the stud welder.
• Mains connection (item 9, chapter 5.1)
The mains connection is located at the rear side of the stud welder. Use the mains
cable supplied to connect the stud welder to the power supply.
5.1.4 Symbols
5.1.5 Fuse elements
The BMS-6 ISO stud welder is protected by the following fuses:
- Mains supply fuses: 2 x 10 A slow, plug-in unit (item 8, chapter 5.1)
- Charging fuse F1: 6.3 A slow, control board S0-115
- Control fuse F2: 1 A slow, control board S0-115
24
Page 25
BMS-6 ISO
- Fuse for the ventilator (optional) F3: 250 mA slow, S0-115 control board (ventilator is
optionally available)
WARNING
Should it become necessary to replace fuses, only use fuses with the prescribed
electrical values. Oversized fuses could either cause defects on the electrical system
or a fire.
Always disconnect mains plug from the power supply when replacing fuses!
5.2 Preparation for start-up
Connect stud welding gun and earth cables to the stud welder prior to start-up.
5.2.1 Earth connection
• Connect earth cable to earth cable connector (item 6, chapter 5.1) and lock by
turning to the right until stop.
• Connect earth terminal to workpiece.
Ensure optimum contact with workpiece.
5.2.2 Connection of stud welding gun
• Connect welding cable of welding gun to welding cable socket (item 5, chapter 5.1)
and lock by turning to the right until stop.
• Insert control cable into control cable socket (item 4, chapter 5.1) and secure with
both locking screws.
• Please make sure that the connecting instructions for welding guns are complied
with (see relevant operating instructions).
5.2.3 Mains supply
• Compare the nameplate rating (line voltage / current consumption) (item 10, chapter
5.1) with the data (line voltage / fuse protection) of your power supply.
Always comply with the correct line voltage as indicated on the type plate.
Never connect the stud welder to a power supply with the wrong line voltage.
• Insert mains cable into mains connection of stud welder (item 9, chapter 5.1) and
connect to the power supply.
25
Page 26
Only connect stud welder to authorized shockproof sockets. If need be, have an
electrician check whether the socket is earthed.
5.3 Operation
• Switch on mains switch (item 7, chapter 5.1).
The four LED displays (item 2, chapter 5.1) on the front panel of the stud welder
shortly light up after switching the stud welder on.
• Use potentiometer (item 1, chapter 5.1) to select charging voltage according to the
respective stud diameter (see table on the front panel).
• Position gun with welding stud on the workpiece.
When earth connection is made and the stud in the gun touches the workpiece, the
LED "Stud on Workpiece" (item 2, chapter 5.1) lights up.
• Press gun switch. The LED "Release" (item 2, chapter 5.1) lights up and stud
welding process is started.
Note regarding PS-1 stud welding gun
Pull the trigger handle of the PS-1 stud welding gun rapidly to be sure to release the
welding process. Please also refer to chapter 9.2, “Troubleshooting”.
BMS-6 ISO
MORTAL DANGER
Hold the gun steady during the welding process and wait until the welding process has
been completed before removing it vertically from the welded stud. A possible
operating error e.g. the welding gun glides off during welding, is identified by the stud
welder and indicated as failure by LED "Malfunction" (item 2, chapter 5.1) lighting up
(also refer to chapter 9.1 “Error Code”).
After removing the welding gun from the welded stud, the capacitor battery is
recharged. Stud welder is ready for welding again after a few seconds (LED "Ready",
item 2, chapter 5.1 lights up).
Adjustment and installation of stud holder into welding gun and adjustment of spring
pressure are described in the operating instructions of the welding gun (see
appendix).
26
Page 27
BMS-6 ISO
PS-1KI
PS-1 / PS-1K
Ø 2
Ø 2.6
Ø 2
Ø 3
Ø 3
Ø 4
Ø 5
Ø 6
4 - 5
5 - 6
4 - 5
6 - 7
6 - 7
6 - 7
7 - 8
9 - 10
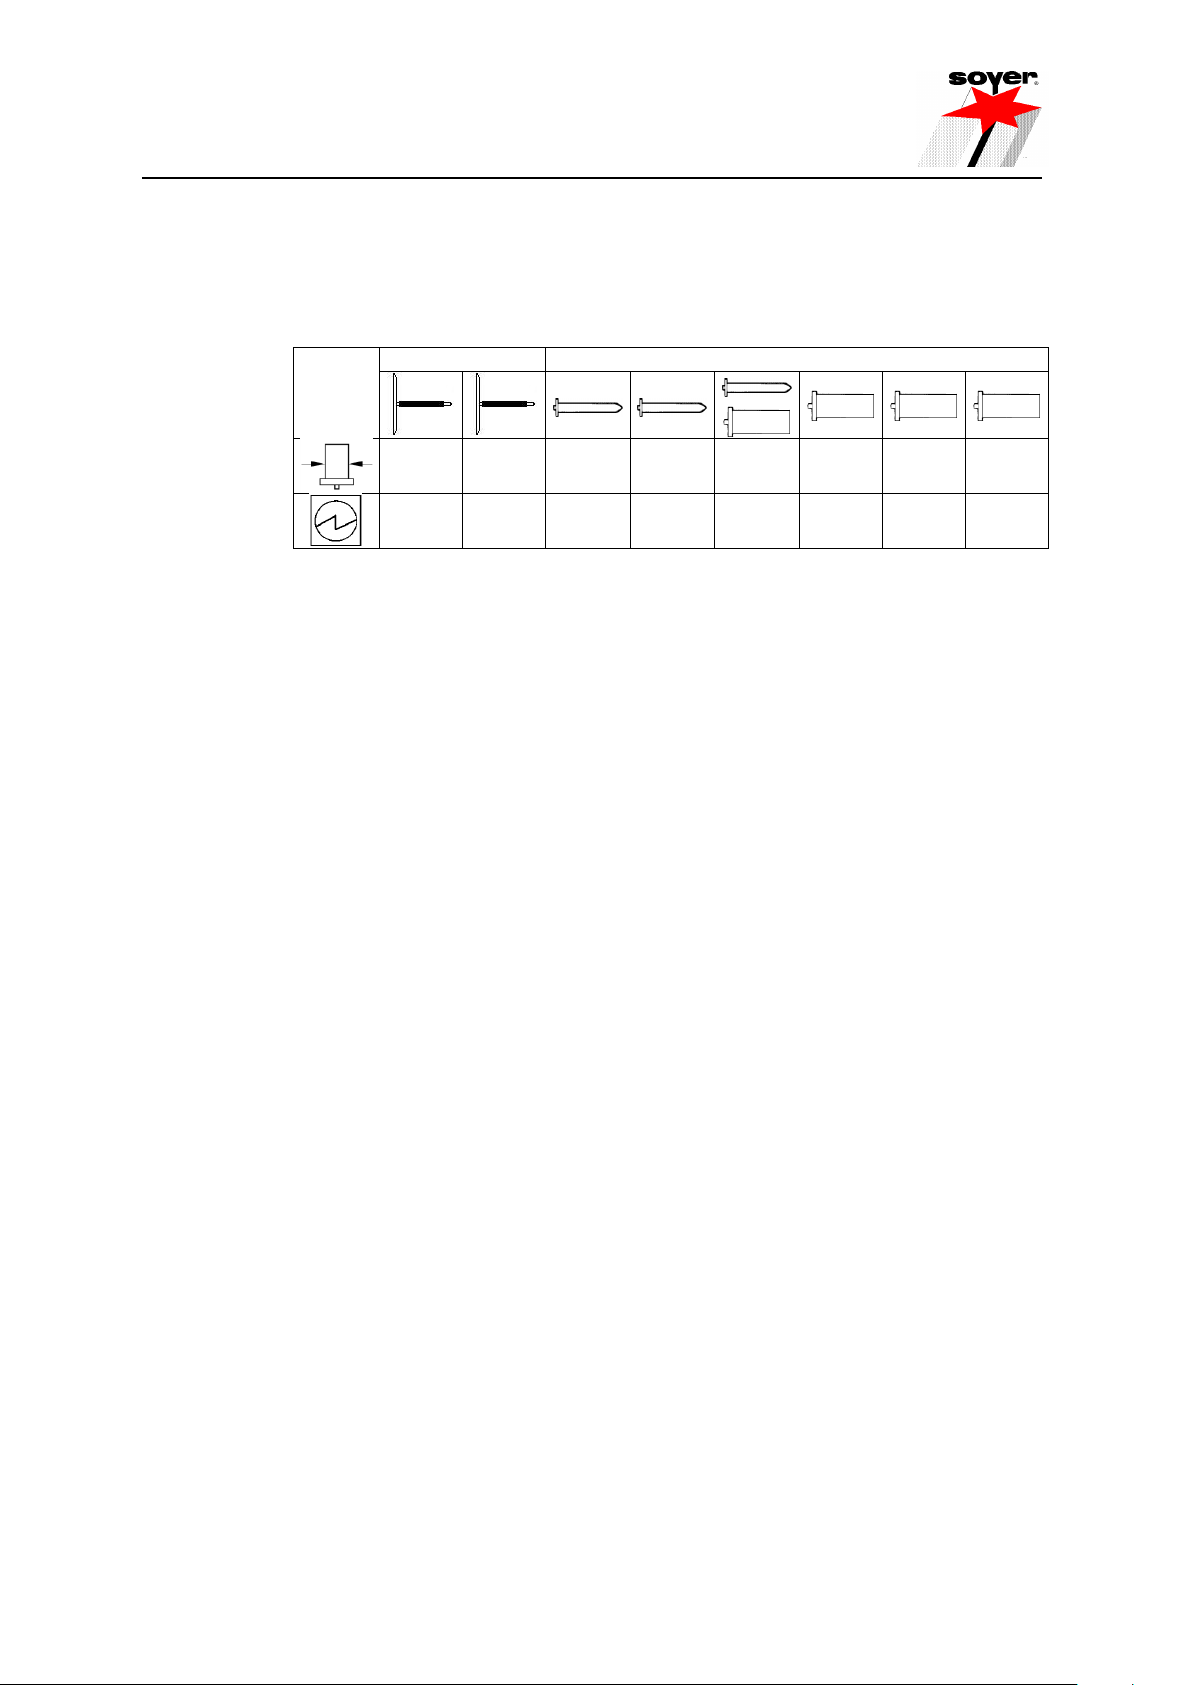
5.4 Welding parameters
The welding parameters of BMS-8N stud welder were determined by means of the
PS-1, PS-1K and PS-1KI stud welding guns.
The charging voltages indicated in the diagram are standard values only. They may
vary from the stated setting depending on material, workpiece thickness and surface
condition of the workpiece.
27
Page 28
BMS-6 ISO
6 Quality control
6.1 General
The DVS Guideline 0905, part 2, of April 1979 is applicable with regard to quality
assurance of stud weld joints. The tests described in this section are written in
simplified terms, following above regulation. They refer to work tests that are carried
out and supervised by the user prior to and during welding.
Heinz Soyer Bolzenschweißtechnik GmbH is member of the German Welding Society
(DVS = Deutscher Verband für Schweißtechnik e. V.), Munich.
6.2 Demands on the company
The company must employ a technical supervisor responsible for welding matters, as
well as qualified operating personnel for stud welding (see DVS Guideline 0905, part
2, section 4).
6.3 Proof of qualification
In the case of components which documentation must be provided for, or stud welding
works which as per DIN 14100, DIN 4113 are subject to acceptance, the processing
company must submit a certificate of competence or a proof of qualification for
working with stud welding equipment (see DVS Guideline 0905, part 2, section 4.1
and 4.2). The proof of qualification applies in particular to the fastening of structures
that are relevant in terms of safety regulations. When being used in the building
industry, only approved base and stud materials may be used (for example, see DIN
4001, section 2.1, certificate of approval for stainless steel ifBT, DIN 4113, part 2).
6.4 Type and scope of test
Provided that the SOYER stud welding equipment is properly used and the materials
are appropriately selected, the strength of the welding joint (welding zone) will always
be stronger than that of the stud or base material.
The following tests are carried out in general practice:
•Standard work test (see DVS Guideline 0905, part 2, section 5.1.2).
•Simplified work test (see DVS Guideline 0905, part 2, section 5.1.2).
6.4.1 Standard work test
Generally, standard work tests have to be carried out and supervised by the user
before welding at a structure and after a certain number of welds has been made. The
number of welds after which a standard work test is required is agreed upon with the
customer.
The standard work test is restricted to the stud diameter, base material and type of
equipment used. It comprises the following tests:
• Visual inspection (all samples)
• Tensile test (at least 3 samples)
• Bend test (at least 3 samples)
28
Page 29
BMS-6 ISO
When in doubt, the test scope should be extended in compliance with DVS Guideline
0905, part 2, section 5.1.1.
6.4.2 Simplified work test
Simplified work tests serve to check the correct setting and function of the equipment.
They are carried out at the beginning of every working shift and after several hours of
interruption.
Simplified work tests include:
• Visual inspection (all samples)
• Bend test (all samples)
6.5 Test execution
6.5.1 Production of samples
The studs for the work test are welded on a sheet metal the minimum size of which is
700 mm x 200 mm. Use the same welding positions and edge distances as on the
component to be welded later. If it is possible and sensible from an economical point
of view, use parts that are identical to those used in later production.
6.5.2 Visual inspection
The visual inspection serves as a rough check for major defects. The uniformity of the
weld is assessed. When in doubt, tensile and bend tests should be carried out.
6.5.3 Tensile test
The tensile test serves to test the metallic bond of the stud with the base metal. At
least 3 studs are welded and then axially loaded by means of an appropriate tension
device until they break. If the customer demands that a certain percentage of the
welded studs should be tested with a specific test load in production, a tension device
with load indicator should be used.
If the stud breaks outside the welding zone, the test is regarded as successful. If it
breaks within the welding zone, however, the fractured surface must be examined.
The unwelded surface may not exceed a maximum 20% of the welding surface. When
in doubt, the breaking load in accordance with DIN 267, part 3, should be determined.
If the quantity of defective studs in one random sample exceeds the acceptance
number specified in DIN 267, part 5, as per AQL 4, it is necessary to find out the
reason for the faults. The setting values must be modified and the test repeated.
6.5.4 Bend test
The bend test is a simple work test which serves to roughly check the setting values
selected. The welding zone is subjected to undefined tension, pressure and bending.
A minimum of three studs is welded and bent to an angle of 30° by means of a tube
that is slipped over the stud. The test is considered as successful, if no superficial
fissure or fracture is detected in the welding zone. The acceptance number in
accordance with DIN 267, part 5, as per AQL 4 must be complied with. If the quantity
of defective parts in one inspection lot exceeds the acceptance number AQL 4 (see
DIN 267), the cause of trouble must be determined and the test repeated again.
29
Page 30
BMS-6 ISO
7 Maintenance
7.1 Stud welder
The stud welder is constructed in such a way that a minimum of maintenance is
required. The stud welder should, however, be cleaned by a specialist at regular
intervals depending on the environmental conditions at the location of use. Any
defects of the stud welder’s control part can be easily eliminated by replacing the
printed circuit boards and/or the clearly arranged fuses.
Before replacing any components, disconnect the mains cable from the mains supply.
Electric and electronic components may only be replaced by a specialist. Contact the
SOYER ® customer service, if necessary.
MORTAL DANGER
DANGER TO HEALTH
Before replacing any components, make sure that the capacitors of the stud welder
have been discharged.
7.2 Cleaning
Cleaning should be carried out once a week depending on how soiled the stud welder
is.
Please pay particular attention to foreign substances in and around the air apertures in
the housing.
7.2.1 Detergents
Almost every detergent is suitable for cleaning purposes. However, please observe
the manufacturer’s specifications on the detergent you intend to use.
7.3 Replacement of components
Defective components may only be replaced by trained SOYER servicemen. Perfect
function of your stud welder can only be guaranteed when original SOYER spare parts
are used.
7.4 Fuses
The BMS-6 ISO stud welder is protected by the following fuses:
- Mains supply fuses: 2 x 10 A slow, plug-in unit (item 8, chapter 5.1)
- Charging fuse F1: 6.3 A slow, control board S0-115
- Control fuse F2: 1 A slow, control board S0-115
- Fuse for the ventilator (optional) F3: 250 mA slow, S0-115 control board
30
Page 31
BMS-6 ISO
DANGER TO HEALTH
Should it become necessary to replace fuses, only use fuses with the prescribed
electrical values. Oversized fuses could either cause defects on the electrical system
or a fire.
MORTAL DANGER
Disconnect the mains plug from the mains supply when replacing fuses.
31
Page 32
BMS-6 ISO
8 Spare parts for BMS-6 ISO
8.1 Spare parts for BMS-6 ISO
Item Qty. Designation Order No.
x x BMS-4 ISO complete P01054
1 1 Front PC Board SO-105 ISO F04674/FA
2 1 Control board SO-115 SMD F04538/FA
3 2 Capacitor 22000 μF / 200 volt E01199
4 1 Earth connector SEM-25 E01964
5 1 Earth socket BEM-25 E01958
6 4 Fine-wire fuse 10A slow E01898
7 1 Fine-wire fuse 6.3A slow E01897
8 1 Fine-wire fuse 1A slow E01892
9 1 Fine-wire fuse 250mA slow (optional) E03535
32
Page 33
BMS-6 ISO
9 Troubleshooting
The following list of errors, their causes and remedies is designed to help you
eliminate any trouble immediately on the spot. If it is difficult or impossible to eliminate
the trouble, please contact the SOYER customer service responsible for your area or
Heinz Soyer Bolzenschweißtechnik GmbH.
For address and telecommunication data, please refer to chapter 1.6 (contacts and
service address).
MORTAL DANGER
Always disconnect the connecting plug from the socket before opening the housing of
the stud welding equipment. Only trained and appropriately qualified personnel are
allowed to carry out works at the electric power supply and welding system.
DANGER TO HEALTH
Only trained and appropriately qualified personnel are allowed to replace components
of the stud welding equipment.
MORTAL DANGER
Before replacing any components, make sure that the capacitors of the stud welder
have been discharged.
33
Page 34
BMS-6 ISO
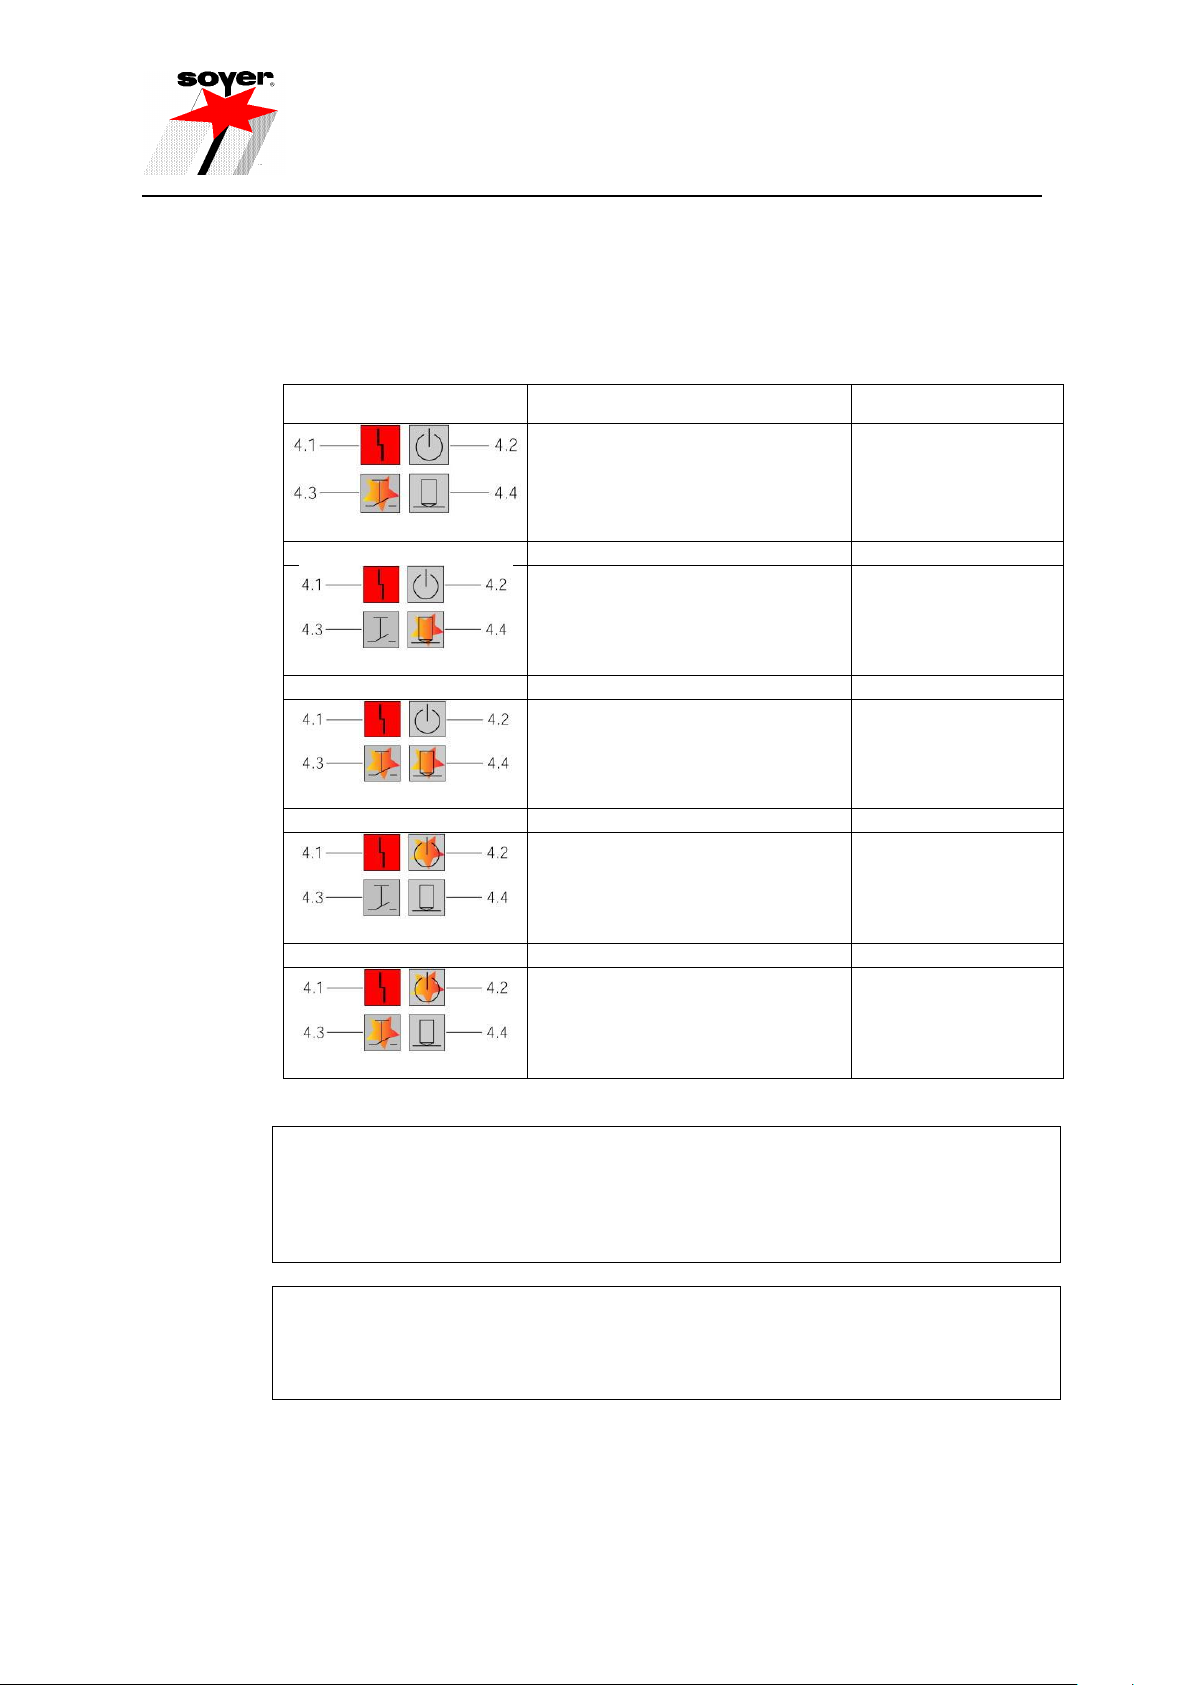
Code
Description
Possible cause
Code E1
Safety circuit activated.
LED 4.1 lights up and LED 4.3 is
blinking
Welding operating
error
Code E2
Charging duration exceeded
LED 4.1 lights up and LED 4.4 is
blinking
Charging fuse is
defective
Code E3
Internal error
LED 4.1 lights up, LED 4.3 and 4.4
are blinking
Safety circuit is
defective
Code E4
Mains voltage is in bad order
LED 4.1 lights up and LED 4.2 is
blinking
Mains voltage
deviation is too large
Code E5
Excess temperature of transformer
LED 4.1 lights up, LED 4.2 and 4.3
are blinking
Excessive welding
cycle
9.1 Error code overview
The stud welder switches off when malfunctions occur. The charging voltage of the
capacitors is internally discharged. An error message appears as code on the
charging voltage display (item 2, chapter 5.1):
The error message is acknowledged by switching the stud welder off and then on
again. If the error message appears again, please inform the customer service
responsible for your area.
If the error message “Excess temperature of transformer” appears, the stud welder
waits till it has cooled down before restarting the welding process.
34
Page 35
BMS-6 ISO
Error
Cause
Elimination
System does not weld, no
sparking
System is not switched on
Switch on system, LED ”Ready” and charging voltage display must
light up
Welding cable or control cable are not connected properly or damaged
Connect cables properly or check for damage. Replace if necessary
Both earth cables are not connected or are not properly connected
and/or earth clamps are not attached to the workpiece
Connect earth cables, attach earth clamps to the workpiece
Welding points and/or earth connection points at the workpiece are not
blank
Prepare workpiece and/or studs
System is switched on,
but does not function
Mains supply is defective
Check mains supply fuse
Fuse of stud welder is defective
Replace defective fuse (see chapter 7.4)
There is no arc even
though system is ready for
operation
Stud without ignition tip or centre mark too deep for the ignition tip
Use stud with ignition tip or reduce centre mark
Control of stud welder or welding gun is defective
Inform SOYER customer service
Stud is too loose in stud holder
Press stud holder together or tighten it
Stud thread scorched
Stud holder worn
Replace stud holder
Varying welding results
Welding energy not correctly adjusted
Adjust welding energy
Cable connections too loose. Transition resistances are generated
Check all cable connections and earth clamps for tight fit
Stud too loose or not fully inserted into stud holder until stop
Insert stud into stud holder until stop. Replace stud holder, if
necessary
Magnetic blowing action. Arc is forced into a certain direction
Alter earth clamp fixture, place iron parts on the edges and/or rotate
welding gun
Intensive sparking, stud
flange almost melted away
Welding energy is set too high
Reset welding energy
9.2 Troubleshooting
35
Page 36
BMS-6 ISO
Error
Cause
Elimination
Stud not welded with total
flange surface, deficient
weld joint strength
Welding energy is set too low
Reset welding energy
Poor earth connection
Check earth cables and earth clamps for tight fit, tighten if necessary
Workpiece surface too soiled
Clean workpiece surface
Stud face deformed
Use new welding studs
Stud projection over stud holder incorrectly set
Set distance between stud holder and stud weld base to 2-3 mm
Spring pressure incorrectly set
Adjust spring pressure
Welding gun in tilted position
Ensure that all three gun legs are simultaneously and evenly
positioned on the workpiece
Base metal not suitable for welding
Use suitable material combinations
System does not weld
Release period of 0.6 sec. exceeded after pressing the trigger switch of
the gun
Trigger handle of PS-1 welding gun too slowly pulled
Trigger switch of gun incorrectly set or defective
Welding gun mechanically defective (e.g. jammed or sluggish piston)
Release period:
For safety and welding quality reasons, the ignition tip of the welding
studs must touch the workpiece and be ignited within 0.6 sec. after
pressing the trigger switch of the gun. The welding process is not
released when exceeding this period of time.
36
Page 37
BMS-6 ISO
10 Transport and storage
The stud welder is robustly designed and has a two-piece metal housing. Owing to the
electronic and mechanic components it should be ensured, however, that transport is
free from vibrations.
The BMS-6ISO stud welder is equipped with a carrying handle for easy transport.
The GK-2 suitcase offers the optimum solution for storing and transporting the BMS-6
ISO stud welder and the PS-1K stud welding gun.
DANGER TO HEALTH
Prevent unauthorized use of the stud welding system by children and
unqualified personnel.
After long system standstill, we recommend having the stud welding system
checked by SOYER® customer servicemen prior to start-up
The housing of the BMS-6 ISO stud welder corresponds to safety class IP 21.
Please observe that this system of protection is not suitable for being operated or
transported in the rain.
11 Terms of warranty
We warrant for this equipment for a period of 12 months in the case of commercial,
professional or equivalent use. When repairs are necessary, we guarantee to
undertake them in our factory in Etterschlag. Parts subject to wear and tear are
excluded.
Any claim to a warranty will be forfeited if damage is caused by improper operation, or
if repairs or interferences have been made by unauthorized personnel, or whenever
accessories and spare parts have been used which do not match our equipment.
We cannot guarantee the perfect function of the stud welder and the quality of welded
joints if welding studs acquired from another company are used.
37
Page 38
BMS-6 ISO
12 Standards and guidelines
• 2014/35/EU Directive on Low Voltage
• 2014/30/EU Directive on Electromagnetic Compatibility
• EN 60974–1 Arc welding equipment - welding current sources
• EN 60974–10 Arc welding equipment - EMC requirements
• DVS Information Sheet 0901 Arc stud welding of metallic materials
• DVS Information Sheet 0902 Drawn arc stud welding
• DVS Information Sheet 0903 Capacitor discharge stud welding with tip ignition
• DVS Information Sheet 0904 Practical information – Arc stud welding
• EN 14555 Arc welding of metallic materials
• EN 13918 Studs and ceramic ferrules for arc welding
• DGUV Regulation 1 Principles of prevention
• 2006/42/EC Machinery Directive
• EN 12100–1 Safety of machinery – Basic terminology, systems engineering
• EN 12100–2 Safety of machinery – Technical principles and specifications
• EN 60204–1 Electric equipment of machinery, general requirements
38
Page 39
Appendix A / PS-1 and PS-1K
1 Adjustment of PS-1 / PS-1K stud welding guns
1.1 Adjustment of stud holder
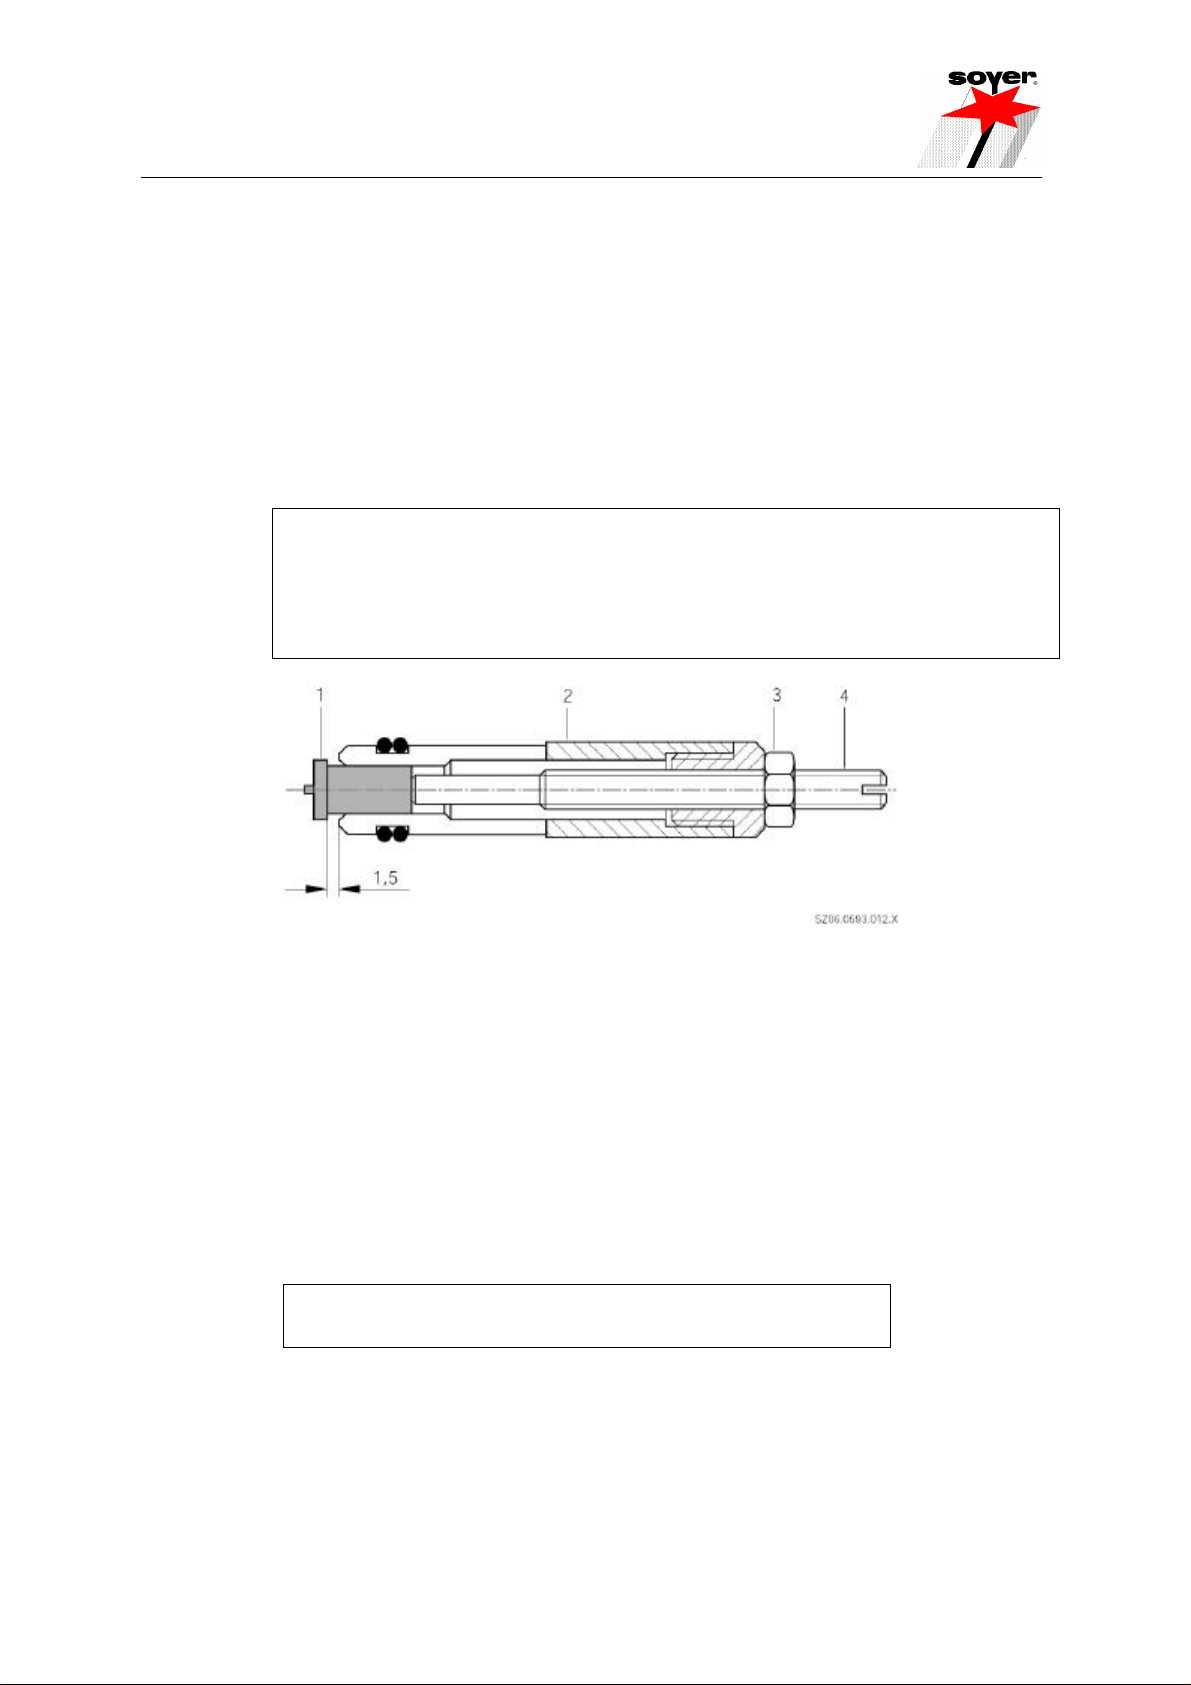
The stud holders of PS-1, PS-3K, PS-0K and PS-1K stud welding guns are
all of the same style. When using long welding studs with the short type PS-0K
and PS-1K welding guns, however, it is necessary to shorten the stud holders'
stop screw (4) correspondingly.
FF
For PS-1, PS-3K, PS-0K and PS-1K guns, use the standard stud holder with
adjusting screw, having a length of 40 mm! Ensure that the maximum stud
length does not exceed 35 mm!
1 Stud 3 Lock nut
2 Stud holder 4 Stop screw
Different stud holders are required for different stud diameters.
Adjust the stud holder as follows:
• Loosen lock nut (3)
• Insert stud (1) into stud holder.
The top edge of the stud flange must project for about 1.5 mm from the front
edge of the stud holder.
FF The stud must come into contact with the stop screw (4).
• Adjust stop screw (4) in the stud holder by turning it until the distance from
the top edge of the stud flange to the front edge of the stud holder is 1.5 mm.
R
• Secure stop screw (4) by means of lock nut (3)
Appendix A /2
Page 40
Appendix A / PS-1 and PS-1K
1.2 Installation of stud holder into PS-1 and PS-3K stud welding guns
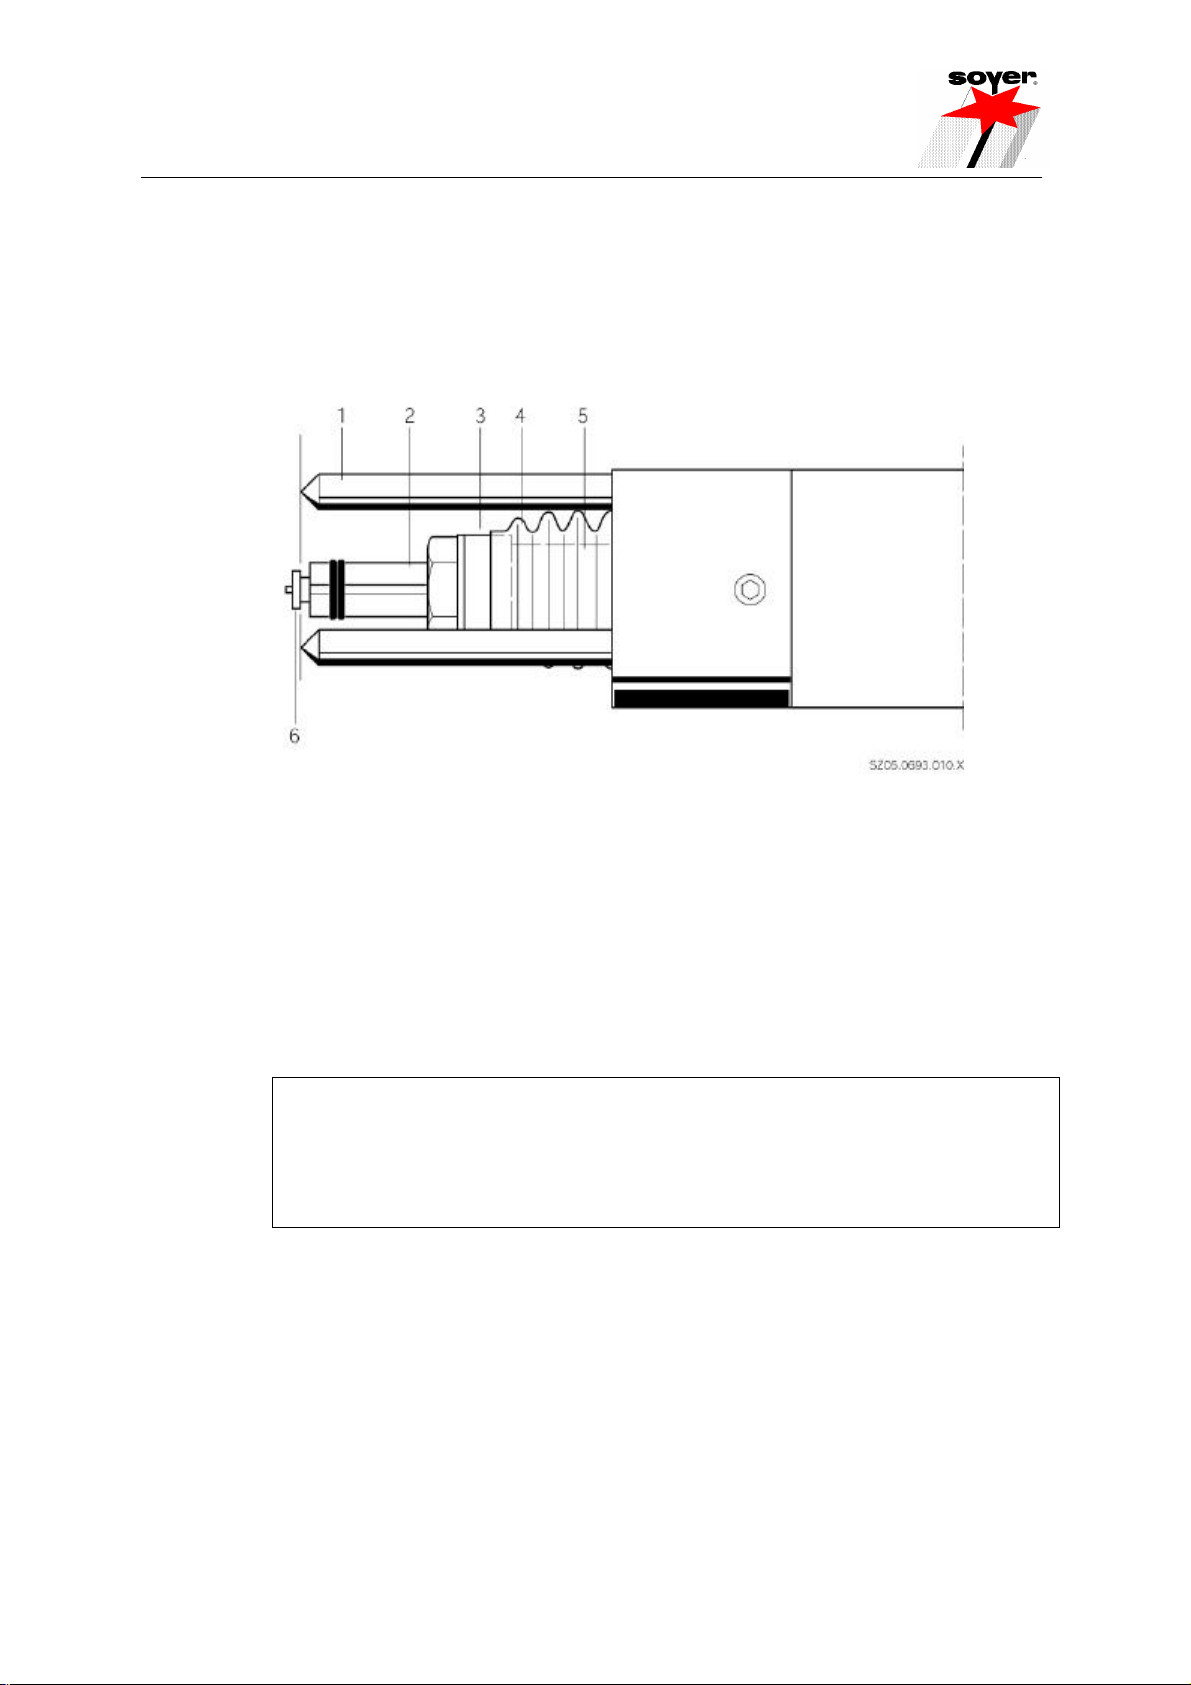
The illustration below shows how to install the stud holder into the PS-1 and
PS-3K stud welding guns.
1 Gun leg 4 Bellows
2 Stud holder 5 Spring piston
3 Sleeve nut
• Loosen sleeve nut by means of socket wrench SW 14 .
• Insert stud holder (2) into spring piston (5) until it stops.
• Tighten stud holder (2) by means of the sleeve nut (3).
FF
The stud flange must project beyond the top of the gun legs or the support tube
for the thickness of the flange. If need be, remove stud holder and correct the
projection by means of the stop screw.
Appendix A /3
Page 41
Appendix A / PS-1 and PS-1K
R
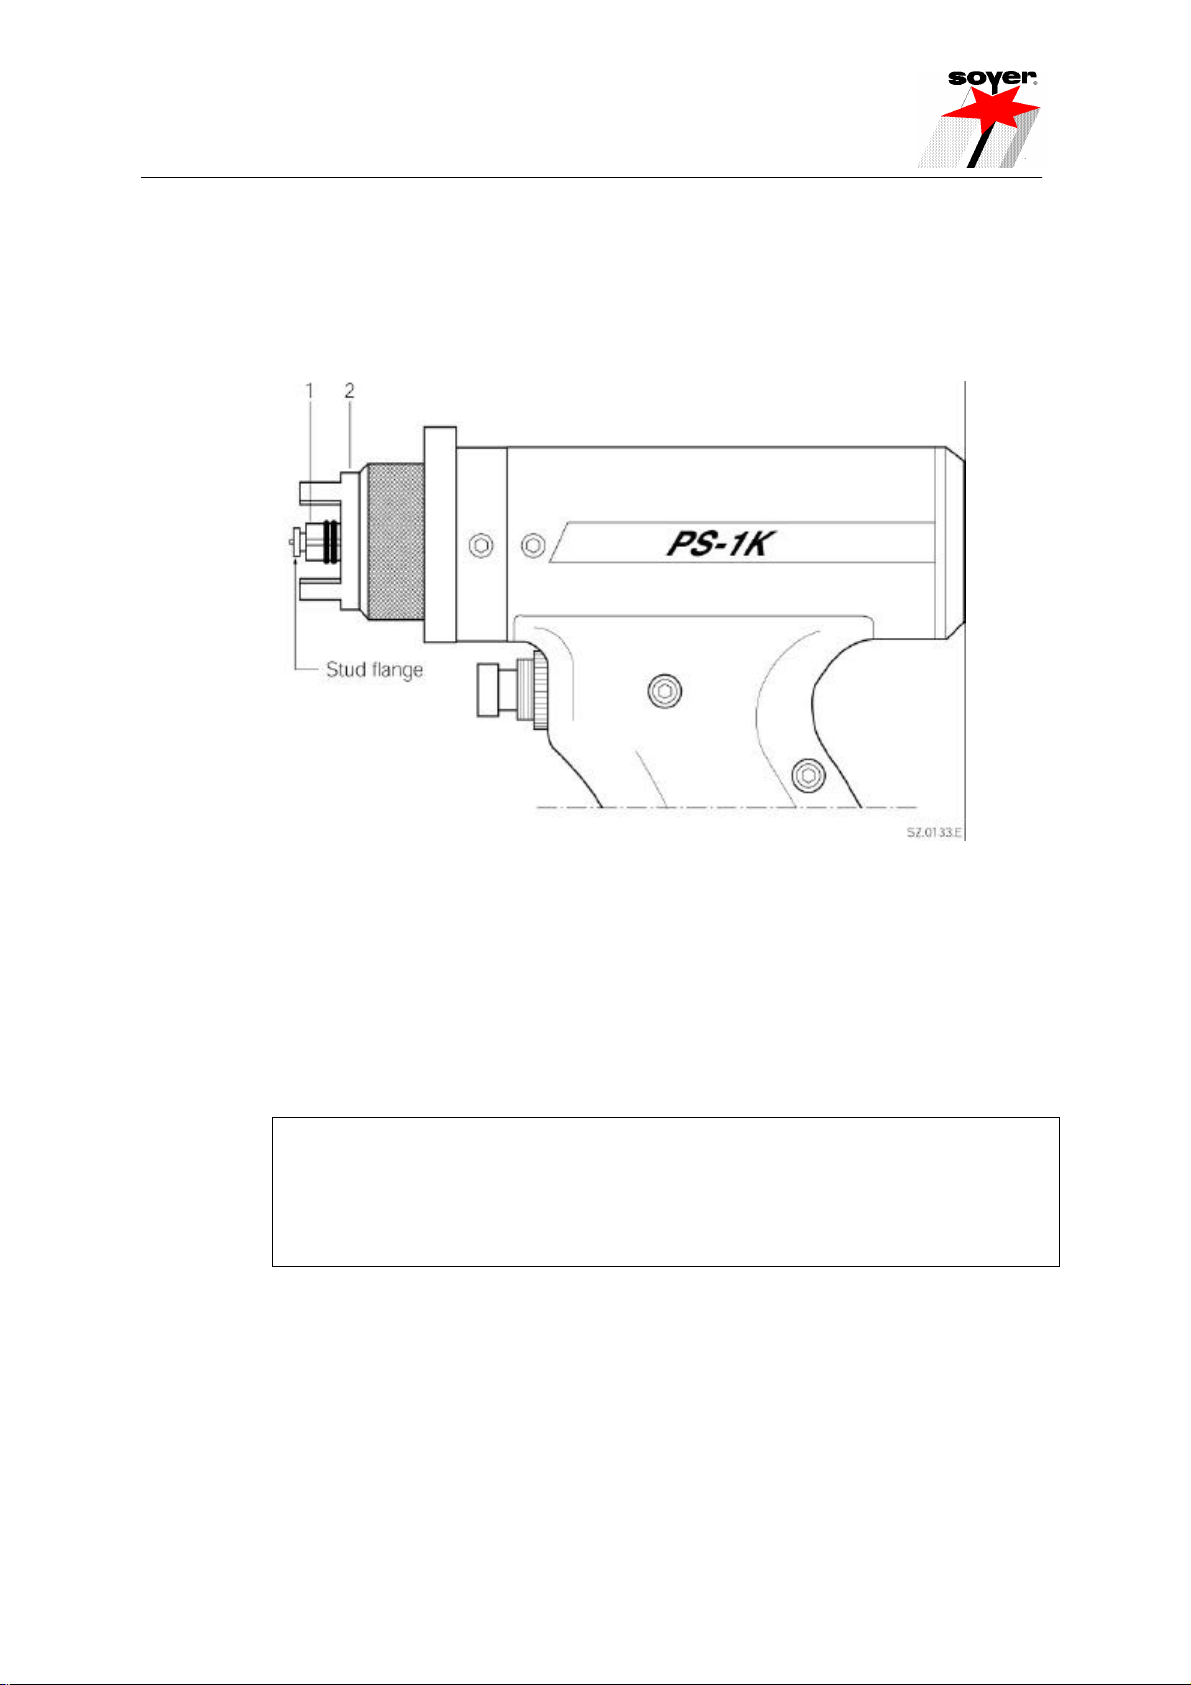
1.3 Installation of stud holder into PS-1K and PS-0K stud welding guns
The illustration below shows how to install the stud holder into the PS-1K stud
welding gun. These instructions also apply to PS-0K stud welding gun.
1 Stud holder 2 Support tube
• Loosen sleeve nut by means of socket wrench SW 14 .
• Insert stud holder (1) into spring piston until it stops.
• Tighten stud holder (1) by means of the sleeve nut.
Remove the support tube (2) to easily install the stud holder.
FF
The stud flange must project beyond the top of the gun legs or the support tube
for the thickness of the flange. If need be, remove stud holder and correct the
projection by means of the stop screw.
Appendix A /4
Page 42
Appendix A / PS-1 and PS-1K
1.4 Adjustment of spring pressure
The pressure with which the stud is pressed against the workpiece during the
welding process is called spring pressure.
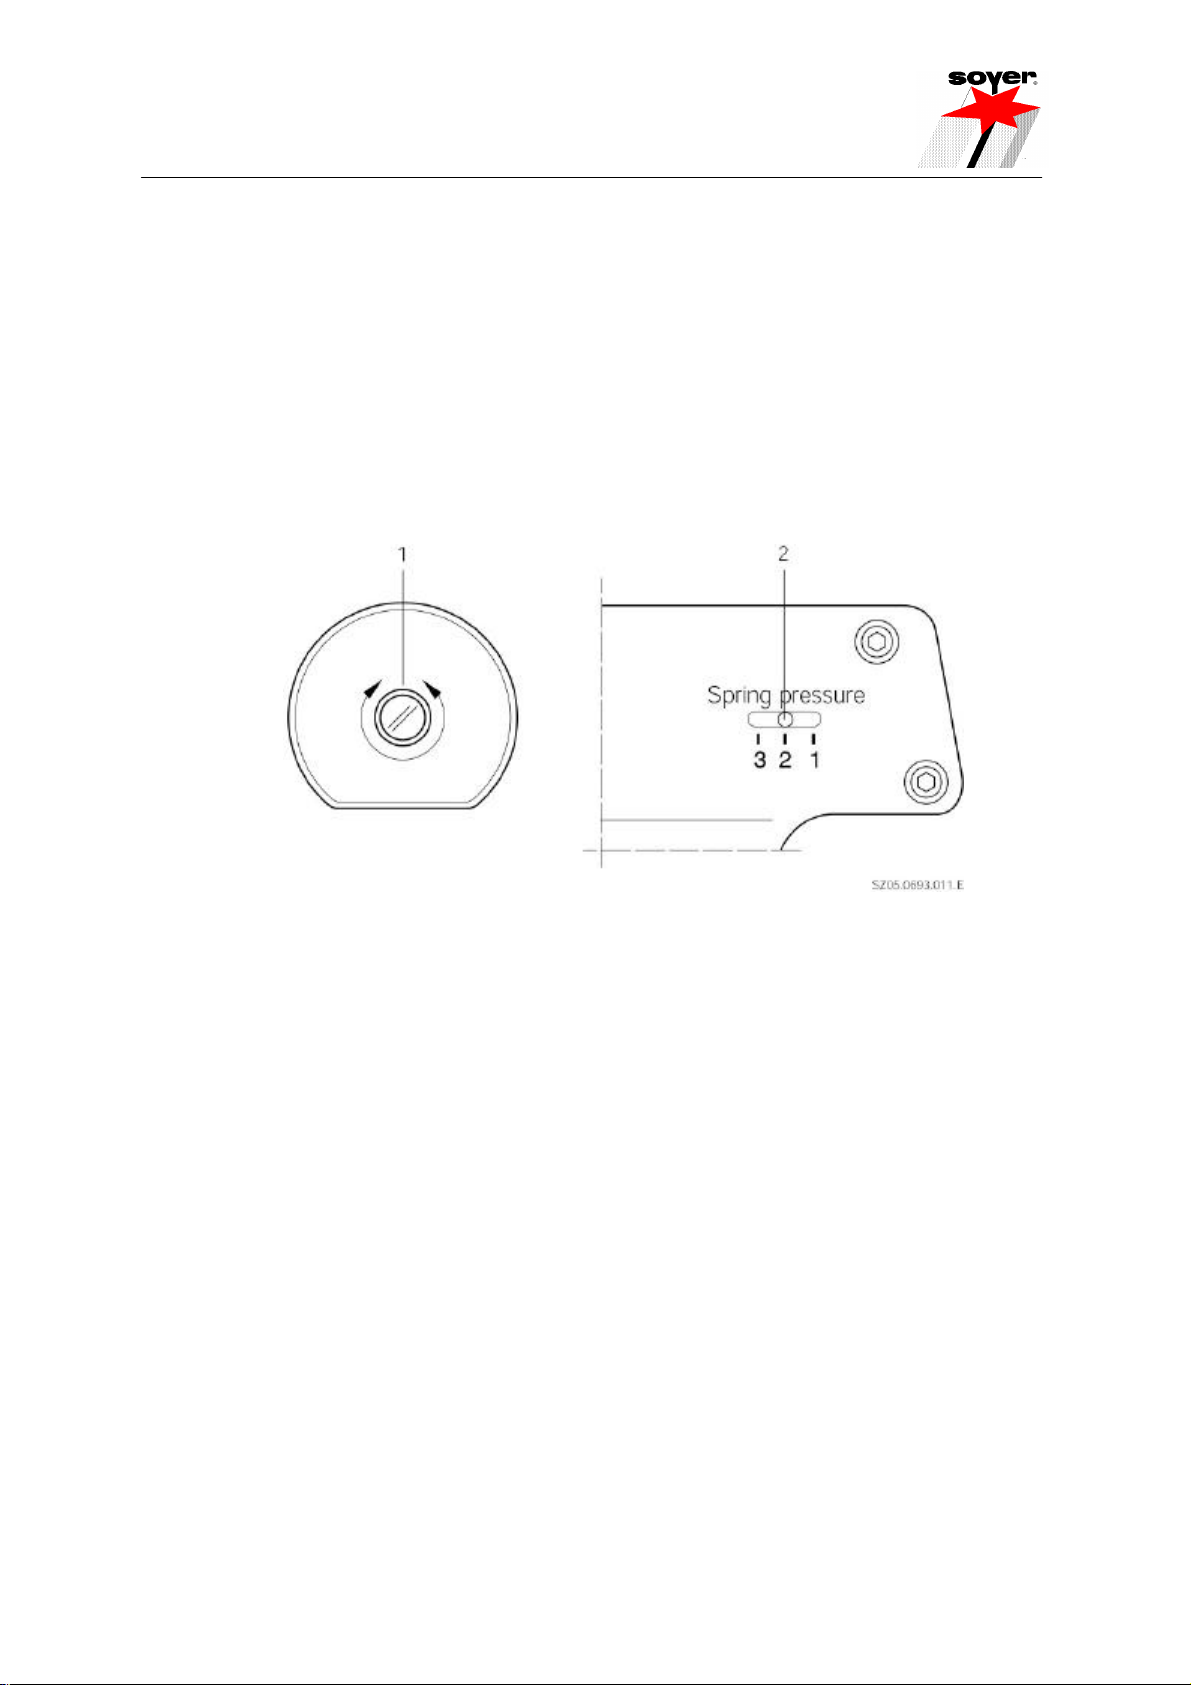
The illustration below shows how to adjust the spring pressure of PS-1 stud
welding gun which is equipped with a spring pressure indicator. The PS-3K
stud welding gun is equipped with a similar spring pressure indicator. The PS0K and PS-1K welding guns do not have a spring pressure indicator.
1 Adjusting screw 2 Spring pressure indicator
The spring pressure for all stud welding guns described here is adjusted by
means of the adjusting screw (1). The adjusted spring pressure is indicated on
the spring pressure scale (2). Adjust the spring pressure as follows:
• Turn adjusting screw (1) to the left until stop
Indicator position 1 = low pressure
• Turn adjusting screw (1) 3.5 turns to the right
Indicator position 2 = medium pressure
• Turn adjusting screw (1) to the right until stop
Indicator position 3 = strong pressure
The adjustment of spring pressure depends on the material of both the welding
stud and the workpiece.
Before starting work, carry out some experimental welds and test them to find
out the optimum adjustment.
Several samples have to be taken during production to ensure constantly good
welding results (see DVS Guideline 0905, part 2, "Quality assurance of stud
welding joints").
Appendix A /5
Page 43
Appendix A / PS-1 and PS-1K
2 Start-up
2.1 Total view
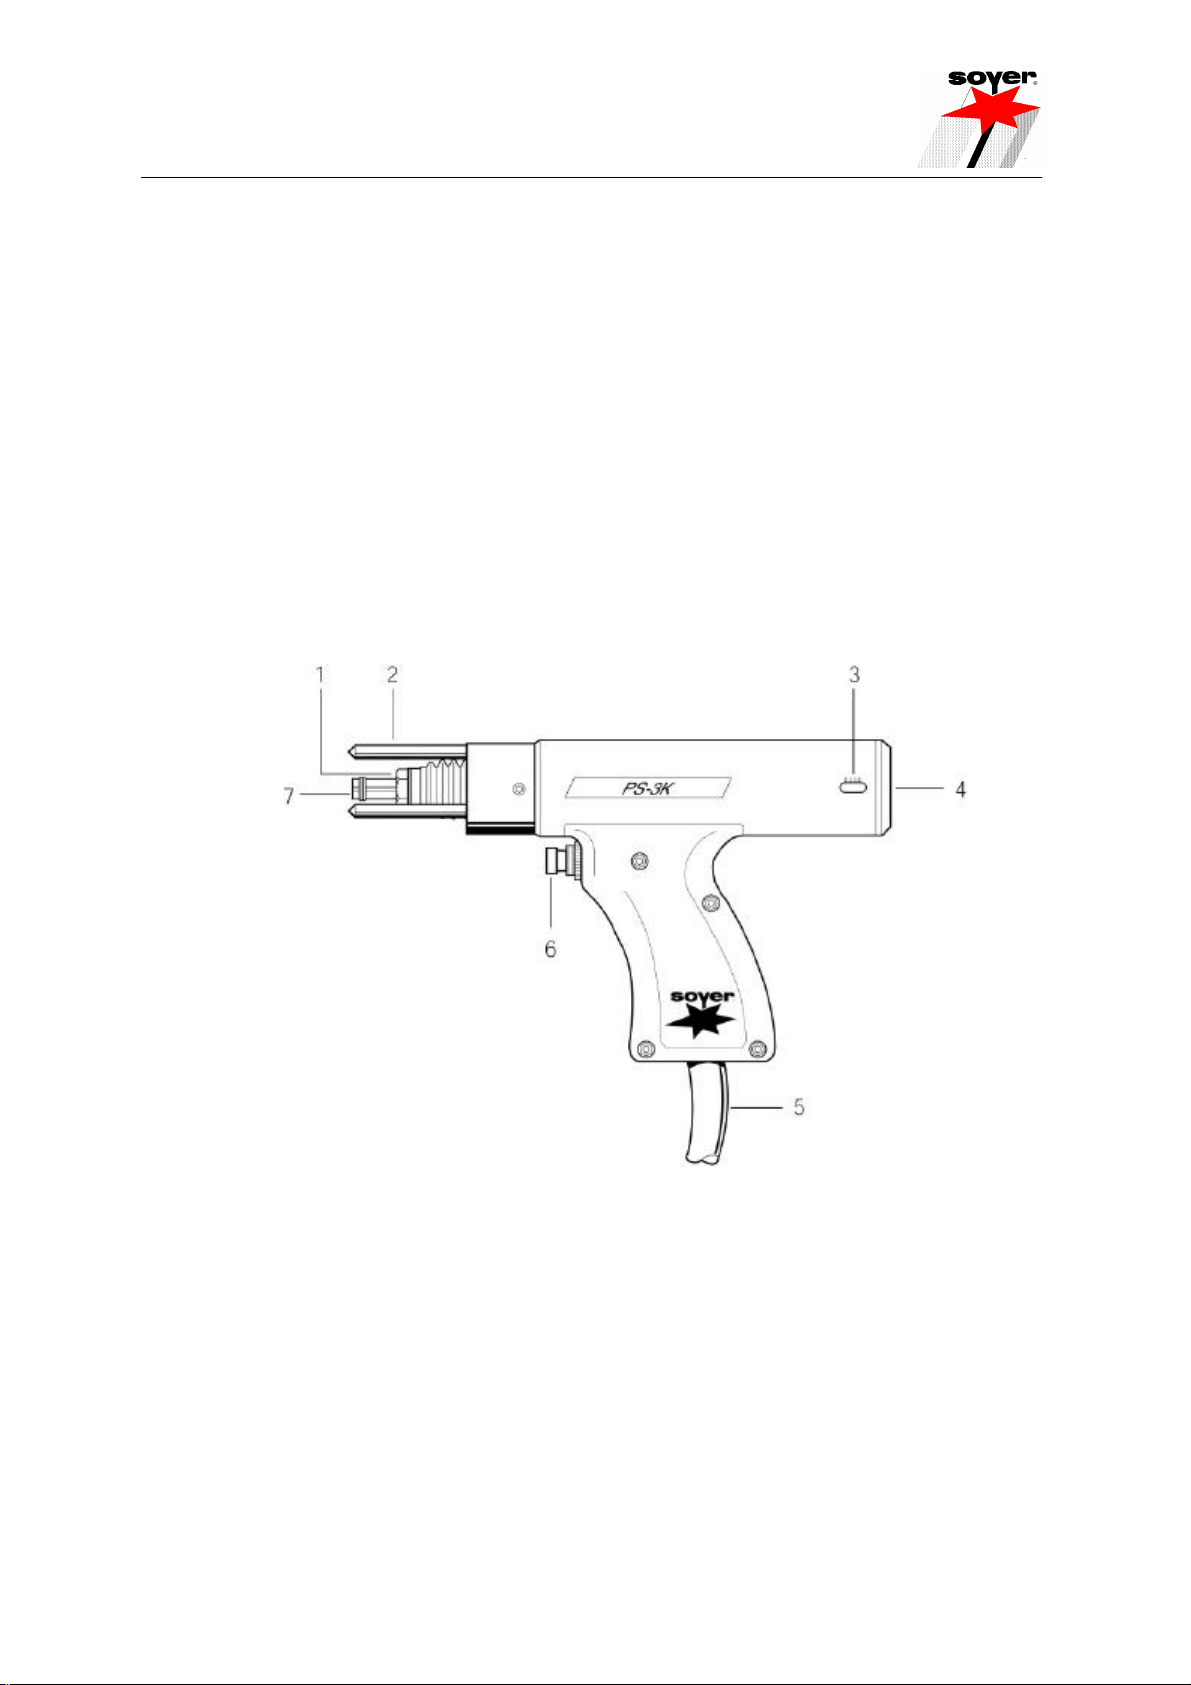
The illustration below shows PS-3K stud welding gun. The indicated
components are only slightly different from those of PS-1, PS-3, PS-0K
and PS-1K stud welding guns.
• The PS-0K and PS-1K stud welding guns are equipped with support tubes
instead of gun legs (2).
• The PS-0K and PS-1K stud welding guns are not equipped with a spring
pressure indicator. The PS-1K stud welding gun is optionally available with
three gun legs.
1 Sleeve nut 5 Connecting cable
2 Gun leg 6 Push-button
3 Spring pressure indicator 7 Stud holder
4 Adjusting screw for spring pressure
Appendix A /6
Page 44
Appendix A / PS-1 and PS-1K
R
2.2 Connecting stud welding guns to stud welder
The stud welding guns are connected to the stud welder by means of the gun
and control cables.
2.3 Operation
• Connect stud welder to earth
• Connect stud welding gun as described in chapter 5
• Adjust welding gun as described in Appendix A, chapter 1
• Connect stud welder to the mains supply
• Adjust stud welder for the welding studs to be used
• Insert welding stud into stud holder
• Position stud welding gun on the workpiece and press push-button
Appendix A /7
Page 45
Appendix A / PS-1 and PS-1K
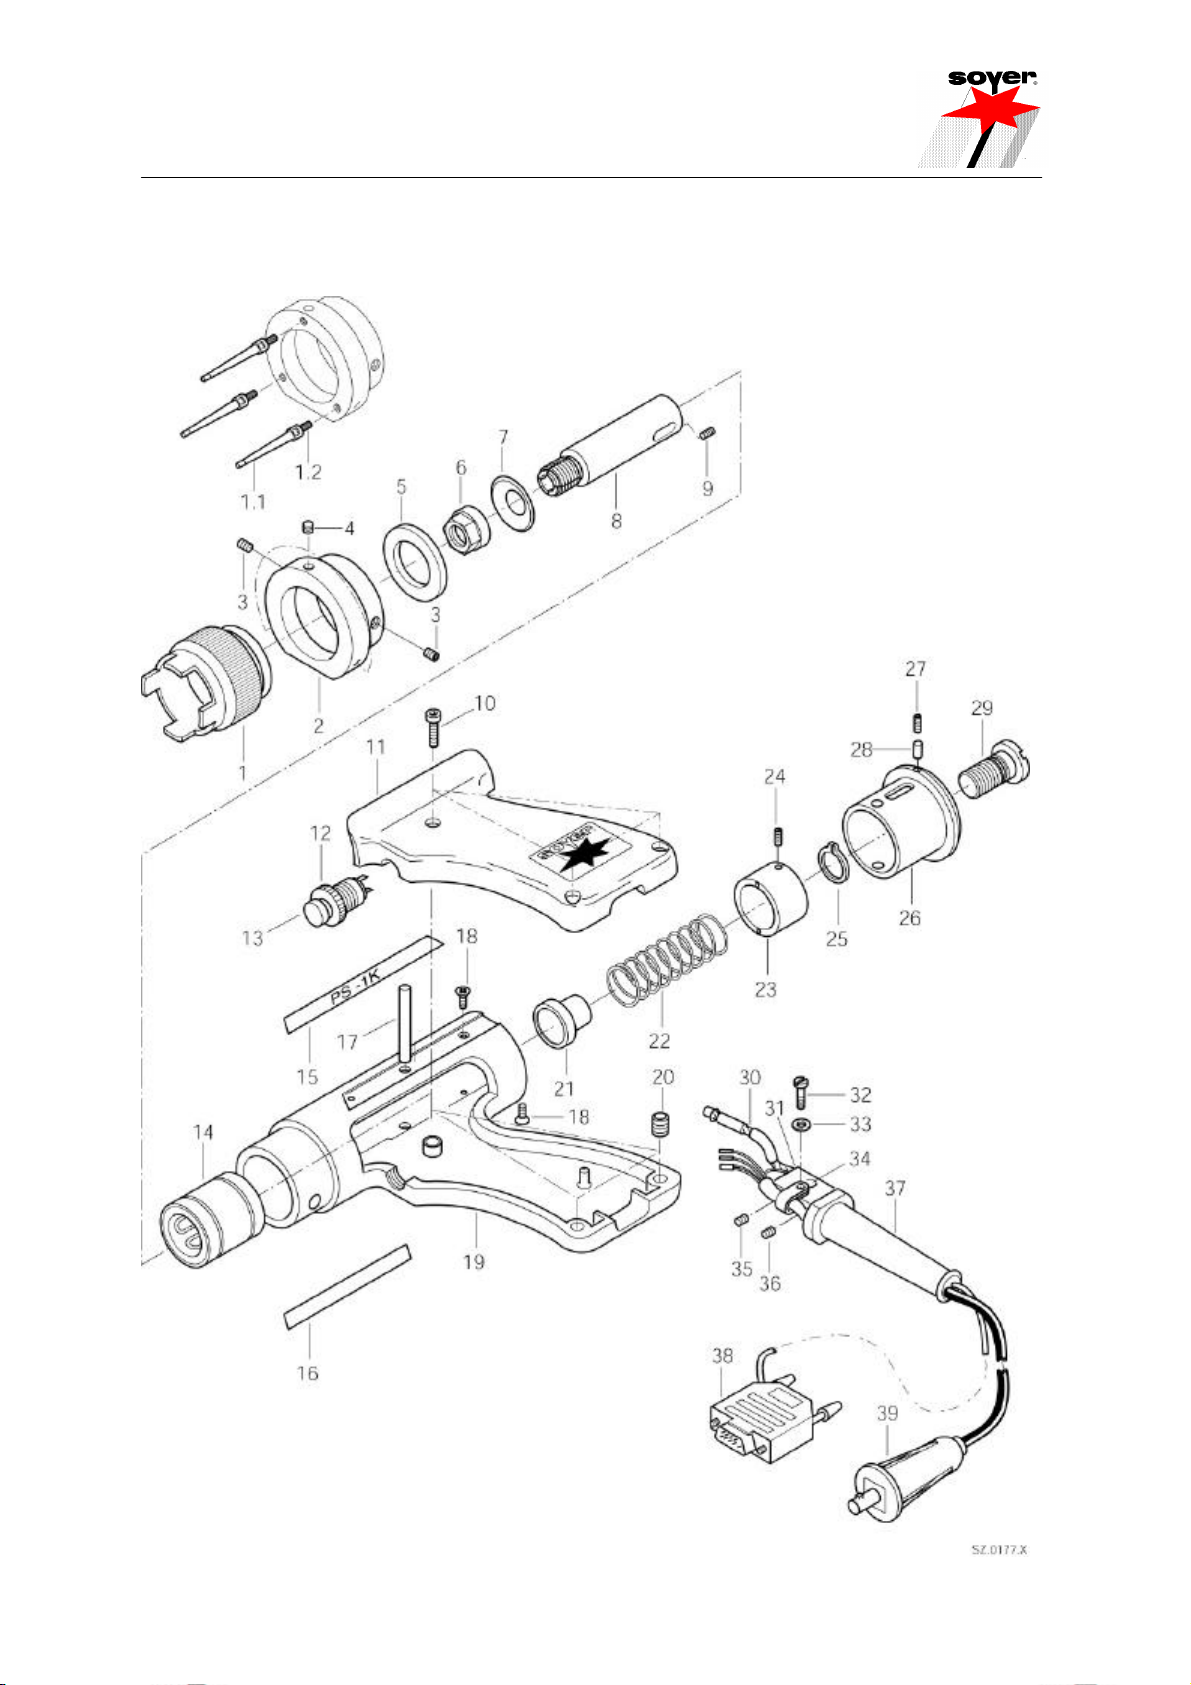
3 Spare parts
3.1 Spare parts list for PS-1K stud welding gun (new model)
Item Qty. Description Order No.
X X Complete PS-1K stud welding gun (new model) P02117
1 1 Support tube Ø 30 mm F03813
1.1 1 3 gun legs (option) F03890
1.2 1 3 grub screws (option) M01338
2 1 Support tube retainer F03812
3 1 Grub screw M6 x 5 M03541
4 3 Grub screw with spring, M4 x 10 M03542
5 1 Insulating ring F03823
6 1 Sleeve nut F01469
7 1 Bellows F02989
8 1 Working piston F03815
9 1 Grub screw M4 x 6 M01315
10 3 Cheese-head screw M01998
11 1 Gun half shell, small (contained in item 19) not numbered
12 1 Push-button, 1-pole E02103
13 1 Cap, PVC E02104
14 1 Ball bearing bush F03824
15 1 PS-1K gun label M02042
16 1 Gun label, company address M01601
17 1 Cylindrical pin 6m6 x 36 M03594
18 2 Flat-head screw M3 x 6 M01561
19 1 Gun housing, complete F03811/FA
20 2 Insert nut M4 x 6 M01809
21 1 Spring retainer F03814
22 1 Pressure spring F03891
23 1 Adjustable adapter F02397
24 1 Grub screw M4 x 8 M01333
25 1 Locking ring M01374
26 1 Split taper socket F02402
27 1 Grub screw M4 x 6 M01315
28 1 PVC pin F03128
29 1 Adjusting screw F01729
30 1 Earth cable, complete F02405/FA
31 1 Strain relief F01715
32 1 Cheese-head screw M4 x 10 M01087
33 1 Spring ring M4 M01074
34 1 PVC clip M01387
35 1 Grub screw M5 x 8 M01337
36 1 Grub screw M8 x 8 M02108
37 1 Anti-kink sleeve E02349
38 1 Control cable E02101
39 1 Gun cable complete with plug comprising: F01100/FA
1 Earth connector SKM-25 E01963
3m Earth cable 25 mm² E02035
Appendix A /8
Page 46
Appendix A / PS-1 and PS-1K
3.2 Exploded view of PS-1K stud welding gun
Appendix A /9
Page 47
Appendix A / PS-1 and PS-1K
Appendix A /10
Page 48
Appendix B / PS-1KI
Appendix B / PS-1KI / Capacitor Discharge
1 Adjustment of PS-1KI stud welding gun................................................................................. 2
1.1 Adjustment of cupped head pin retainer............................................................................. 2
1.2 Installation of cupped head pin retainer into stud welding gun............................................ 3
1.3 Adjustment of spring pressure ...........................................................................................4
2 Start-up.....................................................................................................................................5
2.1 Total view.......................................................................................................................... 5
2.2 Connecting stud welding guns to stud welder..................................................................... 6
2.3 Operation.......................................................................................................................... 6
3 Spare parts............................................................................................................................... 7
3.1 Spare parts list for PS-1KI stud welding gun (new model) ..................................................7
3.2 Exploded view of PS-1KI stud welding gun ........................................................................8
Appendix B /1
Page 49
Appendix B / PS-1KI
1 Adjustment of PS-1KI stud welding gun
1.1 Adjustment of cupped head pin retainer
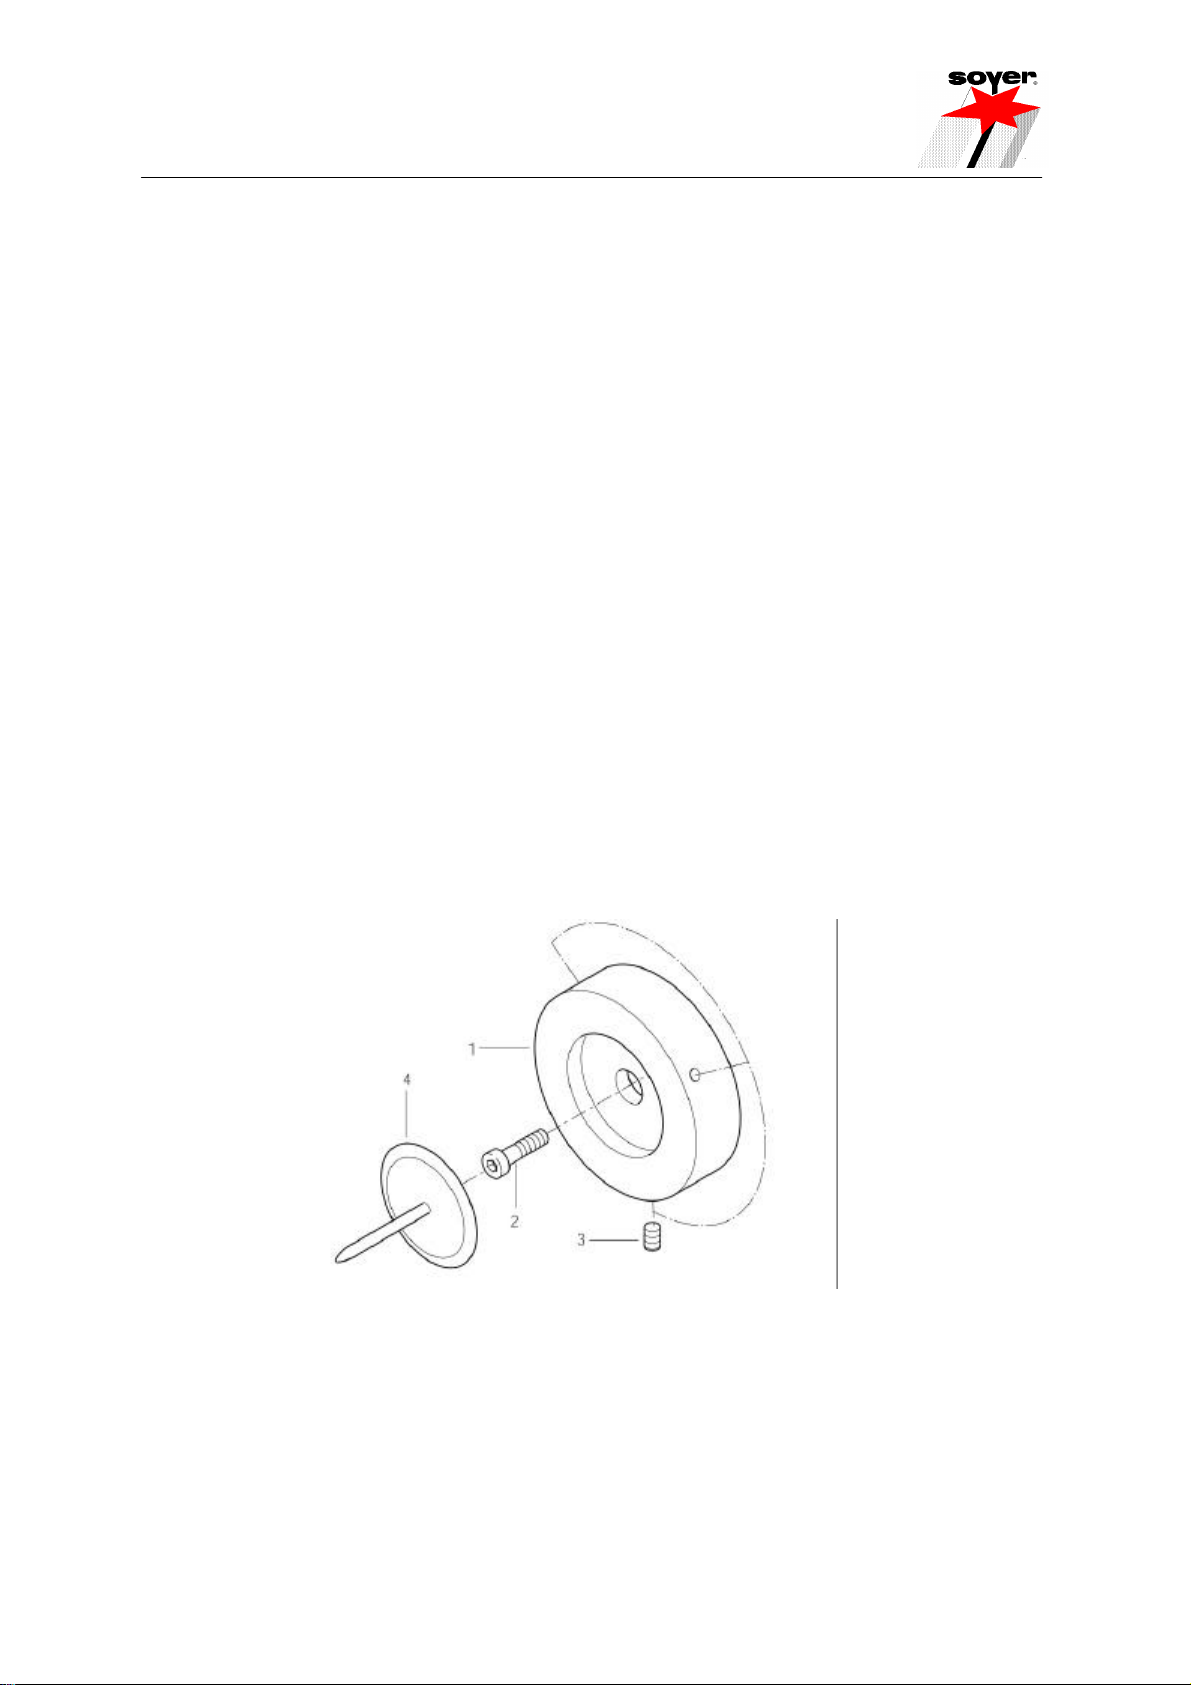
Instead of a stud holder the PS-1KI stud welding gun has a cupped head pin
retainer (1). The adjustment of the stud welding gun is confined to the
adjustment of the spring pressure which holds cupped head pins (4) in the
cupped head pin retainer. The spring pressure, which has to be adjusted by
means of three grub screws (3), determines how firmly the cupped head pin is
held in the cupped head pin retainer. The cupped head pin is inserted against
the spring pressure. Thereby the cupped head pin has to be pressed axially into
the cupped head pin retainer against the spring pressure which is exerted on
three balls located at an angle of 12°.
Adjust the spring pressure as follows:
• Loosen hexagon socket screw (2) and remove cupped
head pin retainer (1) from the support tube.
• Turn grub screws (3) clockwise
= increase of spring pressure (holding force)
• Turn grub screws (3) anticlockwise
= decrease of spring pressure (holding force)
1 Cupped head pin retainer 3 Grub screw
2 Hexagon socket screw 4 Cupped head pin
Appendix B /2
Page 50
Appendix B / PS-1KI
R
1.2 Installation of cupped head pin retainer into stud welding gun
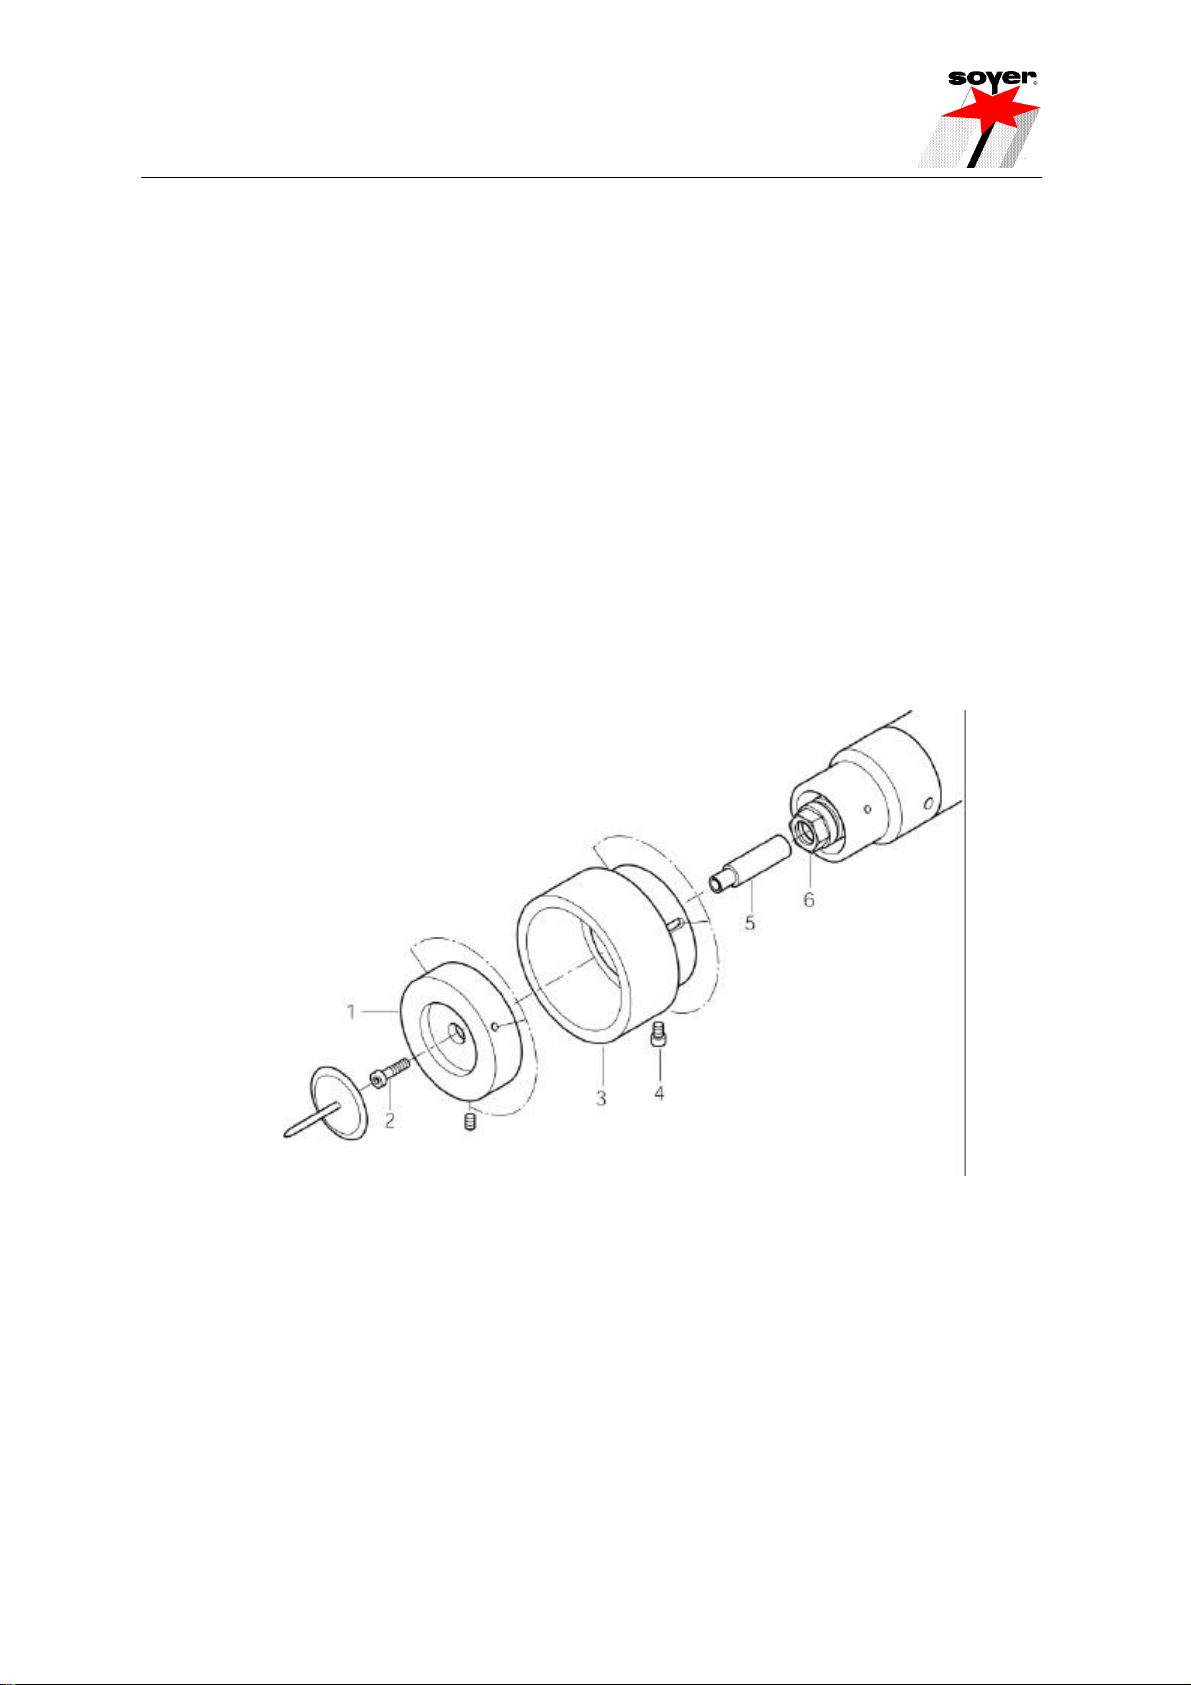
The cupped head pin retainer has to be installed into the stud welding gun as
follows:
• Turn sleeve nut (6) anticlockwise by means of socket wrench SW17.
• Insert retaining pin (5) into spring piston until stop.
• Turn sleeve nut (6) clockwise by means of socket wrench SW17 and secure
retaining pin (5) (hand-tighten the sleeve nut).
• Attach support tube (3) to gun and secure by means of three hexagon socket
screws (4).
• Insert cupped head pin retainer (1) into support tube (3) and secure by means
of hexagon socket screw (2).
1 Cupped head pin retainer 4 Hexagon socket screw
2 Hexagon socket screw 5 Retaining pin
3 Support tube 6 Sleeve nut
After installation of the cupped head pin retainer, check proper function as
follows:
• Press cupped head pin retainer (1) about 5 mm into the support tube (3)
against the spring pressure.
• Release pressure. The cupped head pin retainer is moved into its original
position by the spring pressure. If the cupped head pin retainer gets caught
in the pressed position, it has to be removed and cleaned. Clean the interior
of the support tube as well. If these measures do not have any effect, replace
the components.
Appendix B /3
Page 51
Appendix B / PS-1KI
R
1.3 Adjustment of spring pressure
The pressure with which the stud is pressed against the workpiece during the
welding process is called spring pressure.
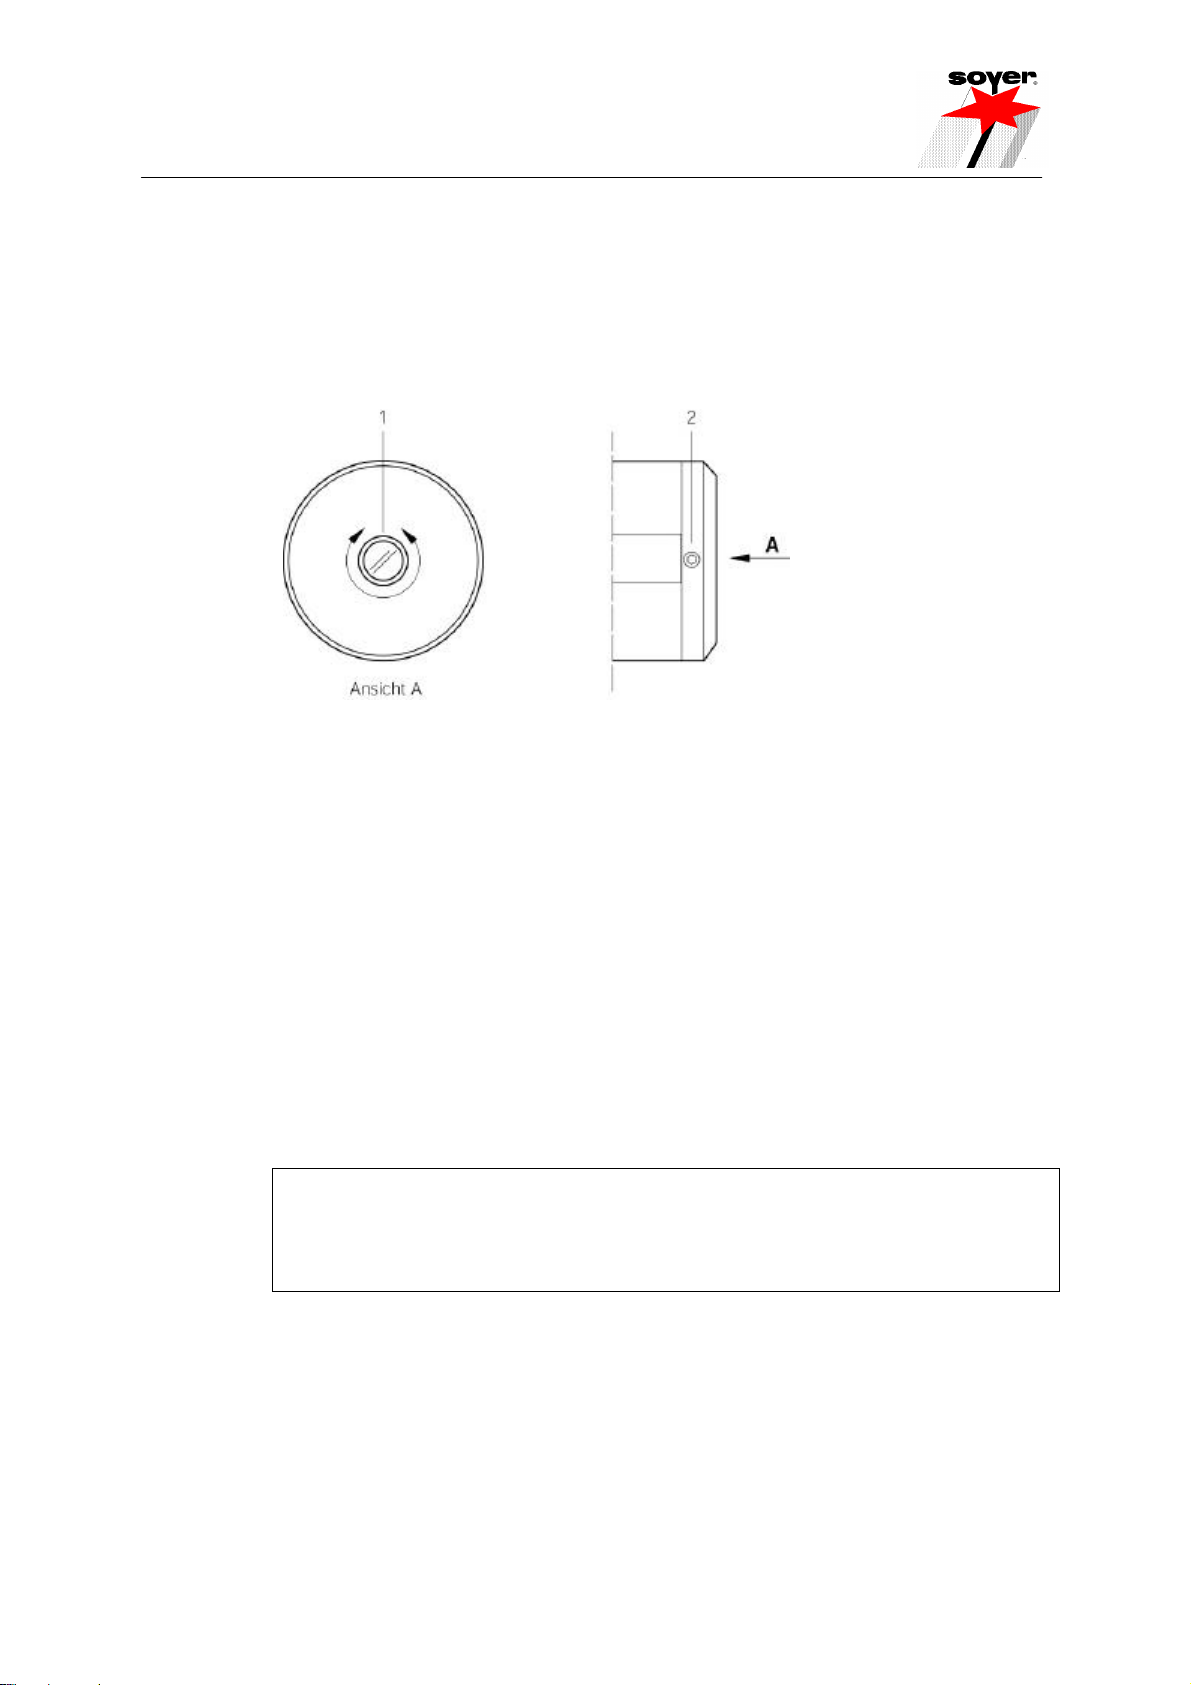
The following illustration shows how to adjust the spring pressure.
1 Adjusting screw 2 Grub screw
Adjust spring pressure by means of adjusting screw (1) as follows:
• Turn adjusting screw (1) anticlockwise until stop
= low pressure
• Turn adjusting screw (1) 3.5 turns clockwise
= medium pressure
• Turn adjusting screw (1) clockwise until stop
= high pressure
• Hand-tighten grub screw (2) by turning it clockwise by means of socket
wrench SW2.
FFAfter having adjusted the spring pressure, fix it by means of the headless
pin (2).
The setting of the spring pressure depends on the material of both welding stud
and workpiece.
Before starting the work, carry out some experimental welds and test them to
find out the optimum setting.
Samples have to be taken during production to ensure constantly good welding results (see DVS Guideline 0905, part 2, "Quality assurance of stud
welding joints").
Appendix B /4
Page 52
Appendix B / PS-1KI
2 Start-up
2.1 Total view
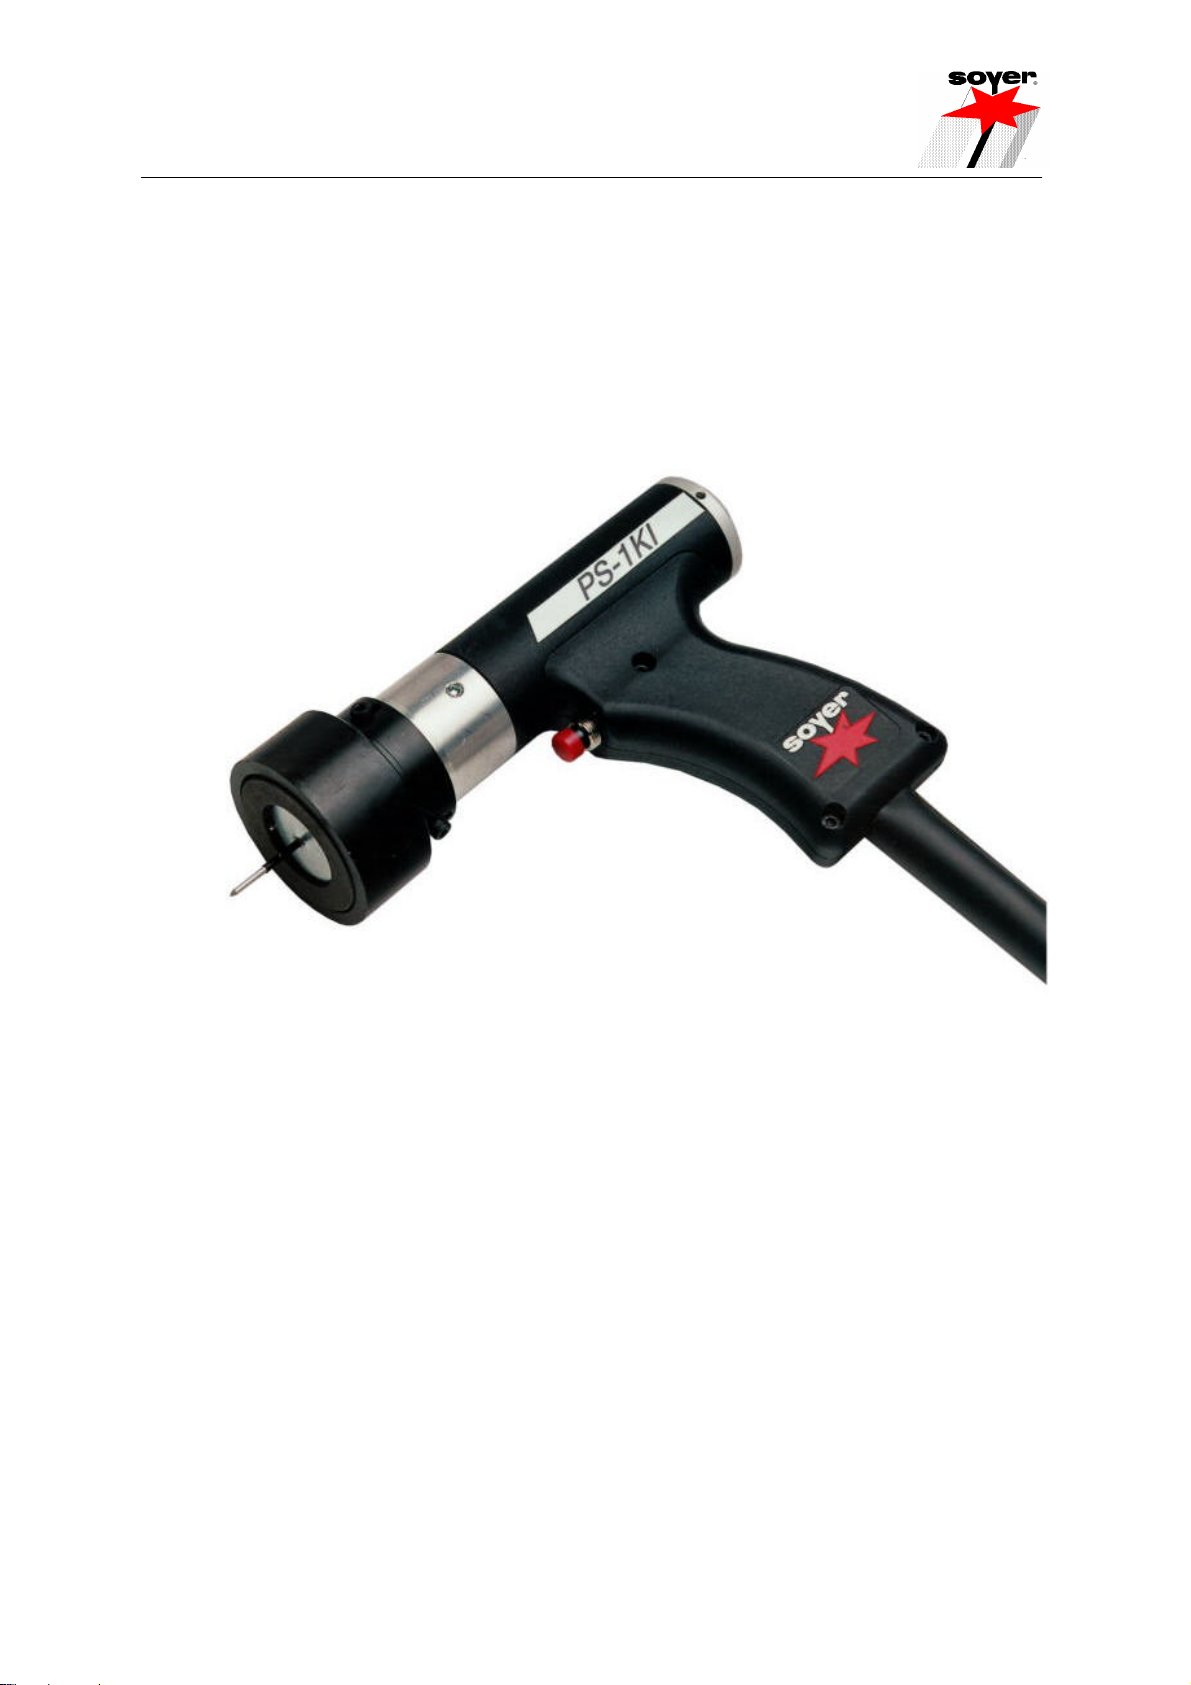
The illustration below shows PS-1KI stud welding gun
Appendix B /5
Page 53
Appendix B / PS-1KI
R
2.2 Connecting stud welding guns to stud welder
The stud welding gun is connected to the stud welder by means of gun
cable and control cable.
2.3 Operation
• Connect stud welder to earth.
• Connect stud welding gun as described in chapter 5.
• Adjust stud welding gun as described in Appendix B, chapter 1.
• Connect stud welder to the mains supply and switch on.
• Adjust stud welder for the cupped head pins to be used.
• Insert cupped head pin into cupped head pin retainer.
• Position stud welding gun on workpiece and press the tip of the cupped head
pin through the insulating jacket on the sheet metal. The welding process is
released automatically when sufficient pressure is exerted on the workpiece.
.
R
Appendix B /6
Page 54
Appendix B / PS-1KI
3 Spare parts
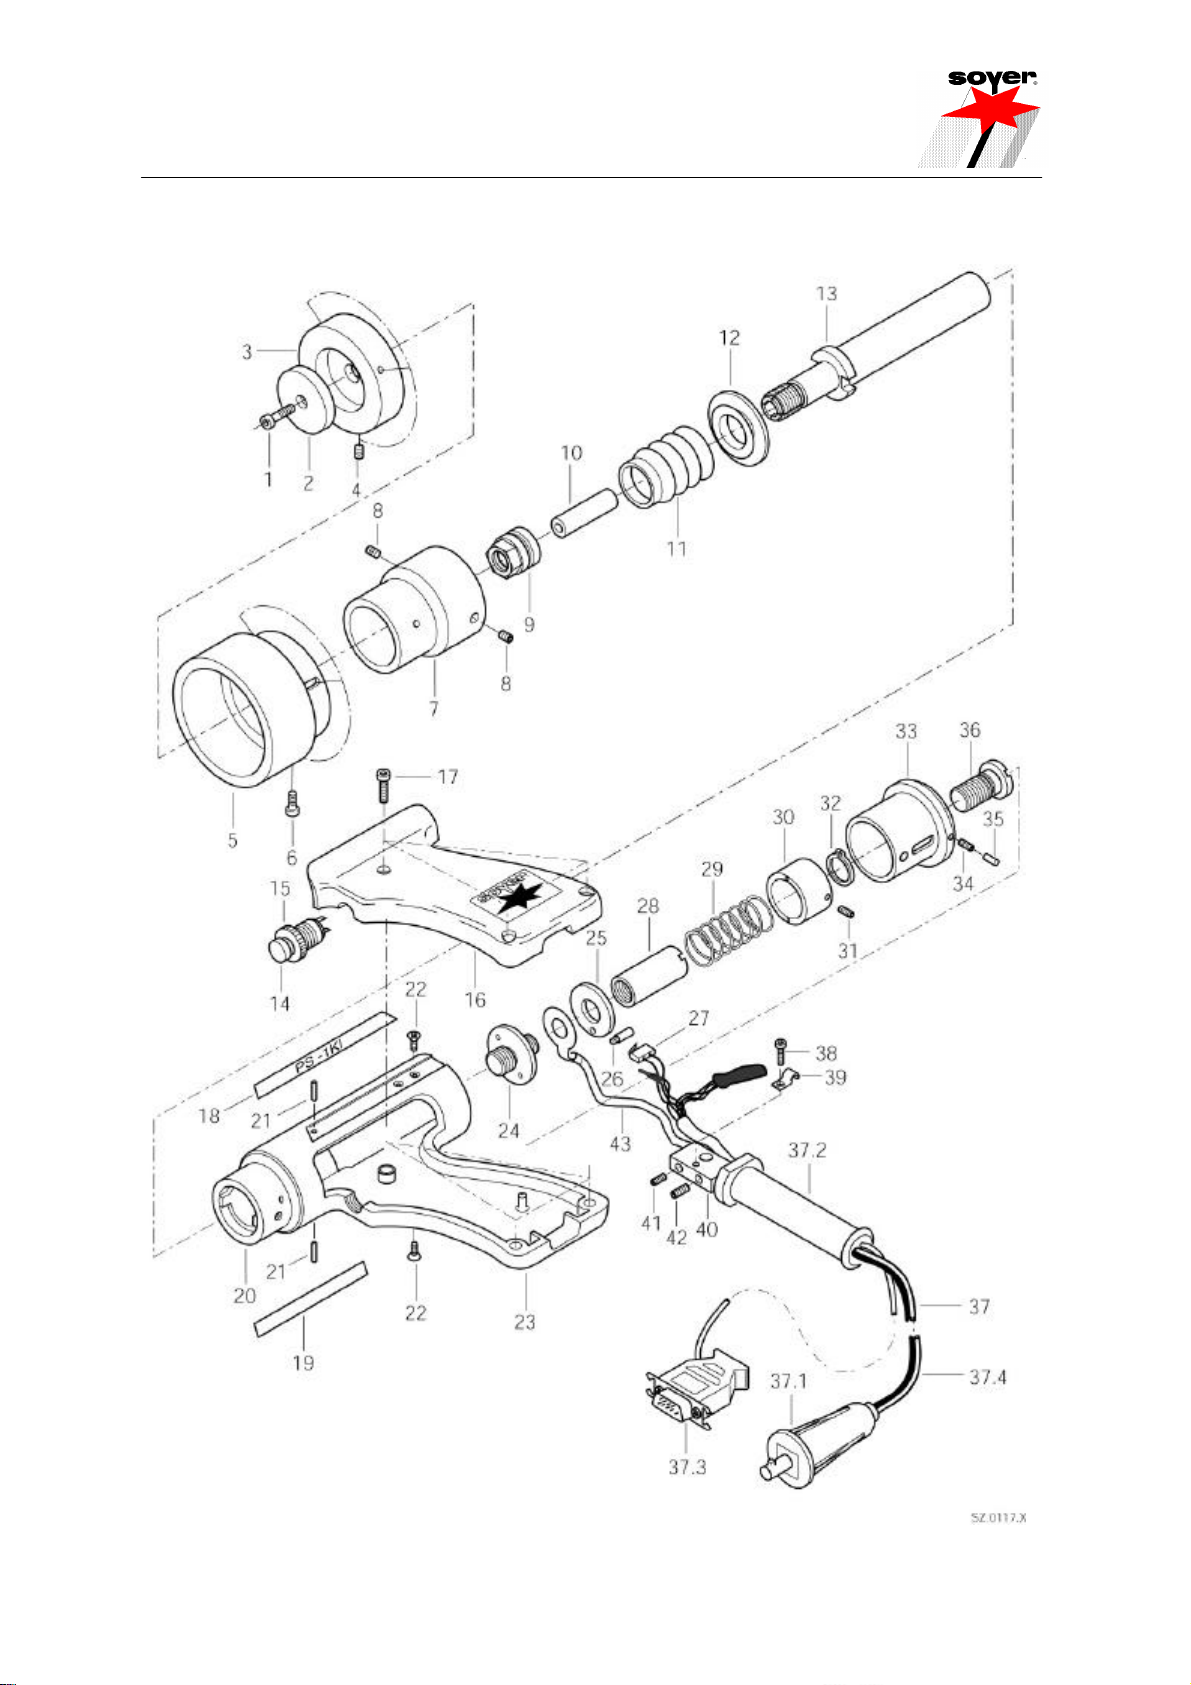
3.1 Spare parts list for PS-1KI stud welding gun (new model)
Item Qty. Description Order No.
X X PS-1KI stud welding gun, complete (new model) P02118
1 1 Cheese-head screw M3 x 12 F03930
2 1 Contact disk M01980
3 1 Cupped head pin retainer F03928
4 3 Grub screw with spring M4 x 10 M03542
5 1 Support tube for cupped head pins F03926
6 3 Fillister head screw M4 x 8 M02021
7 1 Support tube guide F03925
8 2 Grub screw M6 x 6 M01340
9 1 Sleeve nut F01375
10 1 Contact pin F03929
11 1 Bellows F01376
12 1 Delrin ring for bellows F01736
13 1 Working piston F03153
14 1 Cap for push-button E02104
15 1 Push button E02103
16 1 Gun half-shell, small F01717/1
17 3 Cheese-head screw M4 x 8 M01998
18 1 PS-1KI gun label M01111
19 1 Gun label, company address M01601
20 1 Piston guide sleeve F03151
21 2 Clamping sleeve 3 x 10 M01562
22 2 Flat-head screw M3 x 6 M01561
23 1 Gun half-shell, large F01717
24 1 Insulating disk, long F01737
25 1 Pressure disk for switch contact F03170
26 1 Pressure bolt for switch contact F03171
27 1 Micro switch E01215
28 1 Spring retainer F03169
29 1 Pressure spring F01722
30 1 Adjustable adapter F01731
31 1 Grub screw M4 x 8 M01333
32 1 Locking ring M01374
33 1 Split taper socket F02402
34 1 Grub screw M4 x 8 M01333
35 1 PVC pin F03128
36 1 Adjusting screw F01729
37 1 Gun cable, complete F03162/FA
37.1. 1 Earth cable plug E01963
37.2 1 Anti-kink sleeve E02349
37.3 1 Control cable with plug, complete F03987/FA-E
37.4 10m Welding cable 1 x 6 mm² E03639
38 1 Cheese-head screw M4 x 10 M01087
39 1 Cable clip, white E02858
40 1 Strain relief F01715
41 1 Grub screw M5 x 8 M01337
42 1 Grub screw M8 x 8 M02108
43 1 Earth cable, complete F03161/FA
Appendix B /7
Page 55
Appendix B / PS-1KI
3.2 Exploded view of PS-1KI stud welding gun
Appendix B /8
Page 56
Heinz Soyer
Bolzenschweißtechnik GmbH
Etterschlag
Inninger Straße 14
D-82237 Wörthsee
Tel.: ++49-(0) 81 53 / 8 85-0
Fax: ++49-(0) 81 53 / 80 30
Internet: www.soyer.de
E-Mail: [email protected]
 Loading...