

Page 1
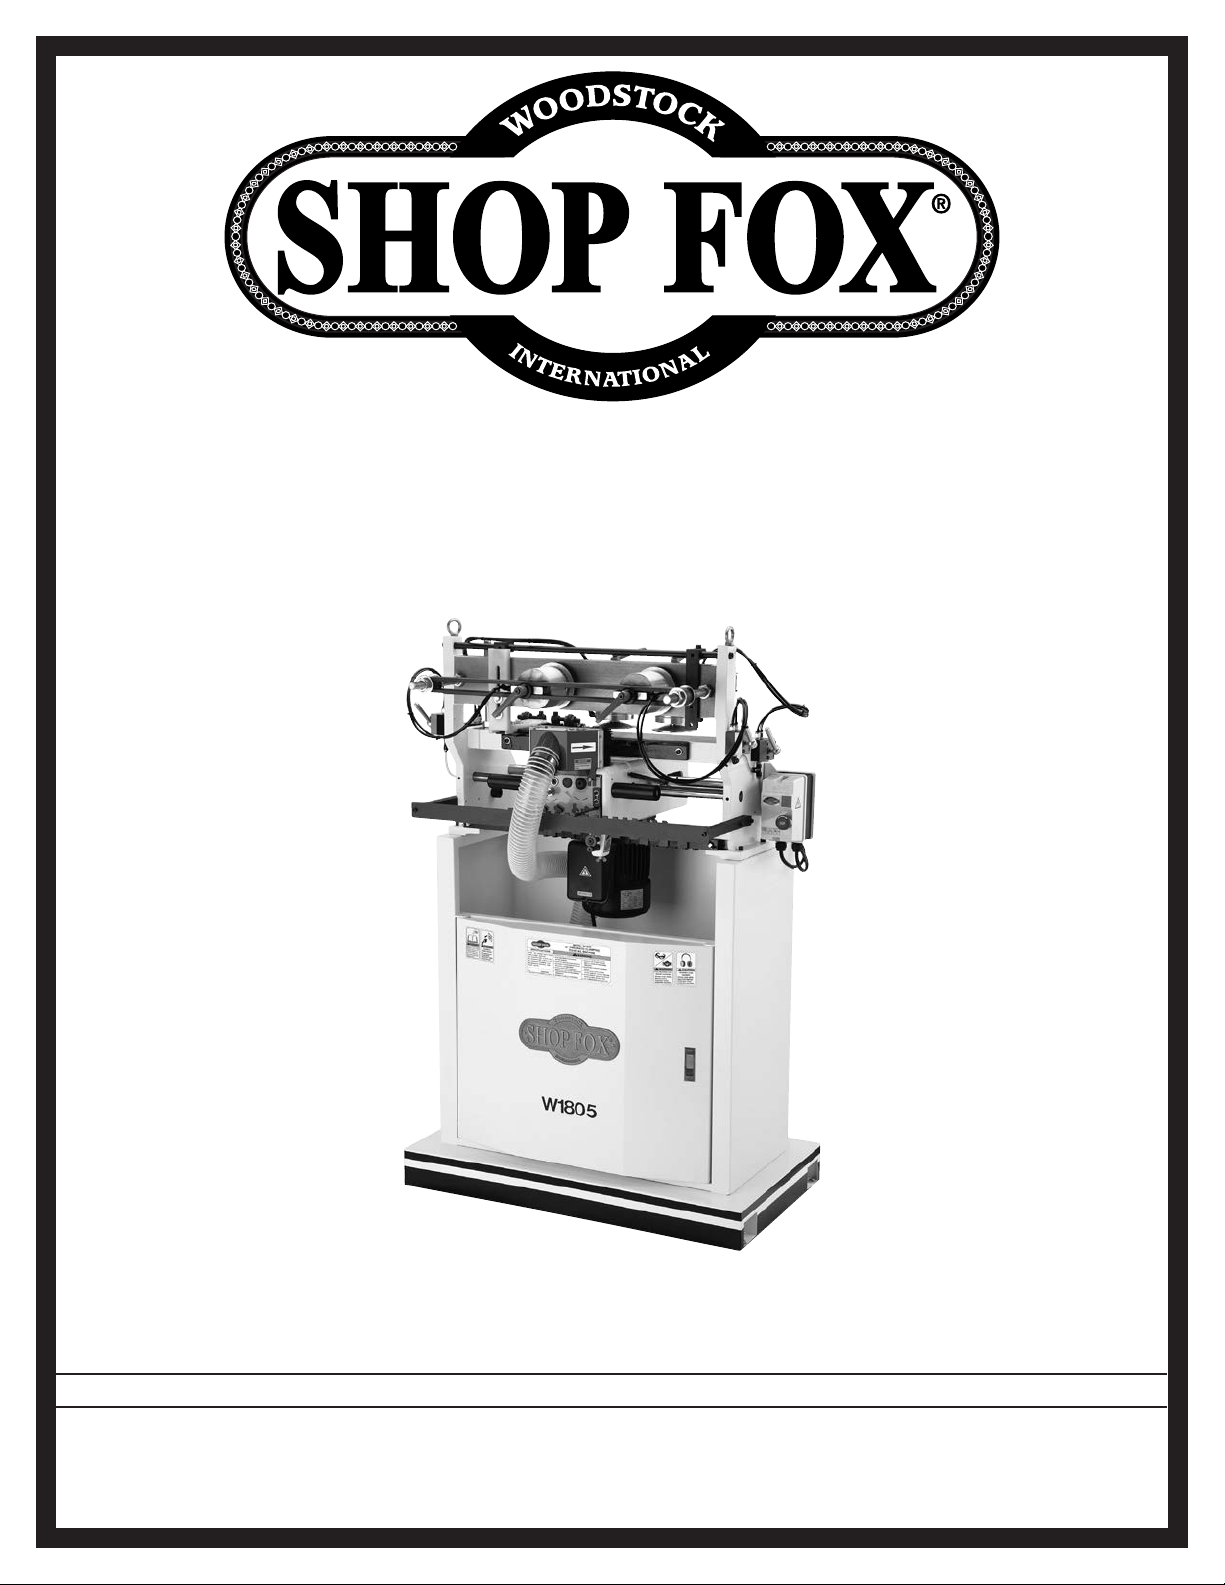
MODEL W1805
161⁄2" DOVETAIL MACHINE
#9341TR
OWNER'S MANUAL
(FOR MODELS MANUFACTURED 7/15)
Phone: (360) 734-3482 • Online Technical Support: [email protected]
COPYRIGHT © JULY, 2007 BY WOODSTOCK INTERNATIONAL, INC. REVISED APRIL, 2020 (JL)
WARNING: NO PORTION OF THIS MANUAL MAY BE REPRODUCED IN ANY SHAPE OR FORM WITHOUT
THE WRITTEN APPROVAL OF WOODSTOCK INTERNATIONAL, INC.
Printed in Taiwan
Page 2
This manual provides critical safety instructions on the proper setup,
operation, maintenance, and service of this machine/tool. Save this
document, refer to it often, and use it to instruct other operators.
Failure to read, understand and follow the instructions in this manual
may result in fire or serious personal injury—including amputation,
electrocution, or death.
The owner of this machine/tool is solely responsible for its safe use.
This responsibility includes but is not limited to proper installation in
a safe environment, personnel training and usage authorization,
proper inspection and maintenance, manual availability and comprehension, application of safety devices, cutting/sanding/grinding tool
integrity, and the usage of personal protective equipment.
The manufacturer will not be held liable for injury or property
damage from negligence, improper training, machine modifications or
misuse.
Some dust created by power sanding, sawing, grinding, drilling, and
other construction activities contains chemicals known to the State of
California to cause cancer, birth defects or other reproductive harm.
Some examples of these chemicals are:
• Lead from lead-based paints.
• Crystalline silica from bricks, cement and other masonry products.
• Arsenic and chromium from chemically-treated lumber.
Your risk from these exposures varies, depending on how often you
do this type of work. To reduce your exposure to these chemicals:
Work in a well ventilated area, and work with approved safety equipment, such as those dust masks that are specially designed to filter
out microscopic particles.
Page 3
Contents
INTRODUCTION .....................................2
Woodstock Technical Support
Machine Specifications
Controls & Features
SAFETY ...............................................6
Standard Machinery Safety Instructions
Additional Safety for Dovetail Machines...... 8
ELECTRICAL .........................................9
Circuit Requirements ............................9
Grounding Requirements
Extension Cords
SETUP .............................................. 11
Unpacking
Inventory
Machine Placement
Cleaning Machine
Lifting & Moving
Mounting to Shop Floor
Assembly
Dust Collection
Air Connection
Test Run
OPERATIONS....................................... 17
General
Dovetail Terminology
Stock Preparation
Dovetail Setup
........................................ 11
......................................... 14
.......................................... 16
.......................................... 17
................................ 10
....................................... 11
................................ 13
................................. 14
.................................. 15
.................................. 20
.......................... 3
............................. 5
............................ 12
............................... 12
.......................... 17
.............................. 18
.................. 2
...... 6
...................... 10
........................ 14
MAINTENANCE .................................... 30
Schedule
Cleaning
Lubrication
SERVICE ............................................ 31
General
Cutter Replacement
Belt Tension
Belt Replacement
Electrical Safety Instructions
110V Wiring Diagram
220V Wiring Diagram (Prewired)
Troubleshooting
PARTS .............................................. 38
Table
Headstock
Stand
Label Placement
WARRANTY ........................................ 45
......................................... 30
......................................... 30
...................................... 30
.......................................... 31
........................... 31
..................................... 31
.............................. 32
................. 33
.......................... 34
............. 35
................................. 36
............................................. 38
....................................... 40
............................................. 42
............................... 44
SAFETYINTRODUCTION
SET UPELECTRICAL MAINTENANCE
OPERATIONS
USE THE QUICK GUIDE PAGE LABELS TO SEARCH OUT INFORMATION FAST!
SERVICE PARTS
Page 4
Model W1805 (For Machines Mfd. Since 7/15)
INTRODUCTION
INTRODUCTION
Woodstock Technical Support
This machine has been specially designed to provide many years of trouble-free service. Close attention
to detail, ruggedly built parts and a rigid quality control program assure safe and reliable operation.
Woodstock International, Inc. is committed to customer satisfaction. Our intent with this manual is to
include the basic information for safety, setup, operation, maintenance, and service of this product.
We stand behind our machines! In the event that questions arise about your machine, please
contact Woodstock International Technical Support at (360) 734-3482 Ext. 2 or send e-mail to:
[email protected]. Our knowledgeable staff will help you troubleshoot problems and process warranty claims.
If you need the latest edition, you can download it from http://www.woodstockint.com/manuals.
If you have comments about this manual, please contact us at:
Woodstock International, Inc.
Attn: Technical Documentation Manager
P.O. Box 2309
Bellingham, WA 98227
Email: [email protected]
-2-
Page 5
Model W1805 (For Machines Mfd. Since 7/15)
MACHINE
SPECIFICATIONS
Phone #: (360) 734-3482 • Online Tech Support: [email protected] • Web: www.shopfox.biz
MODEL W1805
16" PNEUMATIC CLAMPING DOVETAIL MACHINE
Motor
Type ......................................................................................... TEFC Capacitor Start Induction
Horsepower ................................................................................................................. 1 HP
Voltage ...............................................................................................................110V/220V
Prewired .................................................................................................................... 220V
Phase .......................................................................................................................Single
Amps .......................................................................................................................10/5 A
Speed .................................................................................................................. 3450 RPM
Cycle ........................................................................................................................ 60 Hz
Power Transfer .................................................................................................... V-Belt Drive
Bearings ............................................................................................... Sealed and Lubricated
INTRODUCTION
Main Specifications
Cutting Capacities
Maximum Dovetail Height ............................................................................................
Minimum Dovetail Height ...........................................................................................
Maximum Workpiece Thickness ................................................................................... 2
Minimum Workpiece Thickness ....................................................................................
Maximum Workpiece Size ............................................................................ 16
Minimum Workpiece Size ............................................................................ 2
Spindle & Bit Information
Number of Spindles ..................................................................................................... 1
Spindle Speed ................................................................................................18,500 RPM
Dovetail Shank Diameter ..................................................................................
Dovetail Bit ......................................................................... Angle 10° x
Dovetail Templates ................................................................................. 1", 1
Overall Dimensions
5
Machine Size .................................................................................. 35
Machine Weight ........................................................................................................440 Lbs.
Footprint ...................................................................................................... 37" W x 21
Table Height .............................................................................................................. 46
Table Size ....................................................................................................... 24" W x 7
Construction Materials
Cabinet ...................................................................................................... Pre-Formed Steel
Carriage ...............................................................................................................Aluminum
Slide Way ...............................................................................Hardened & Ground Chromed Steel
Table .............................................................................................. Precision Ground Cast Iron
Sliding Guide .................................................................................... Ball Bearing Linear Guides
Paint ............................................................................................................ Powder Coated
⁄8" W x 261⁄2" D x 567⁄8" H
3
⁄8" W x 77⁄8" L
5
⁄8" L, Single Cutter
3
3
⁄16"
3
13
1
⁄2" W x 59" L
1
⁄2" (12mm)
1
⁄2", 2", 21⁄2"
⁄32"
1
⁄4" L
7
⁄16"
3
⁄4" L
⁄4"
⁄8"
-3-
Page 6
INTRODUCTION
Model W1805 (For Machines Mfd. Since 7/15)
Shipping Dimensions
Shipping Crate Size .................................................................................... 42" W x 30" L x 64" H
Shipping Weight ........................................................................................................539 Lbs.
Electrical
Switch ......................................................................................................... Magnetic Switch
Cord Length ................................................................................................................. 9 ft.
Cord Gauge ............................................................................................................ 14 gauge
Recommended Circuit Size at 220V ................................................................................. 15 amp
Recommended Circuit Size at 110V ................................................................................. 15 amp
Recommended Plug Type for 220V ..................................................................................... 6-15
Recommended Plug Type for 110V ..................................................................................... 5-15
Other
Number of Dust Ports ......................................................................................................... 1
Dust Port Size ................................................................................................................. 4"
Approximate Assembly Time ......................................................................................15 Minutes
Warranty ..................................................................................................................2 Year
Country of Origin ....................................................................................................... Taiwan
Machine Highlights
Dual pneumatic clamps for lightning-fast workpiece loading/unloading
1HP, 110V/220V, Motor (prewired 220V)
Included 1", 1
Micro-adjustable cutter controls for precision-fit dovetails
Handles workpieces as large as 2
Once setup, can create a dovetail joined box in under 40 seconds!
1
⁄2", 2", and 21⁄2" dovetail templates
3
⁄8"H x 161⁄2"W x 59"L
-4-
Page 7
Model W1805 (For Machines Mfd. Since 7/15)
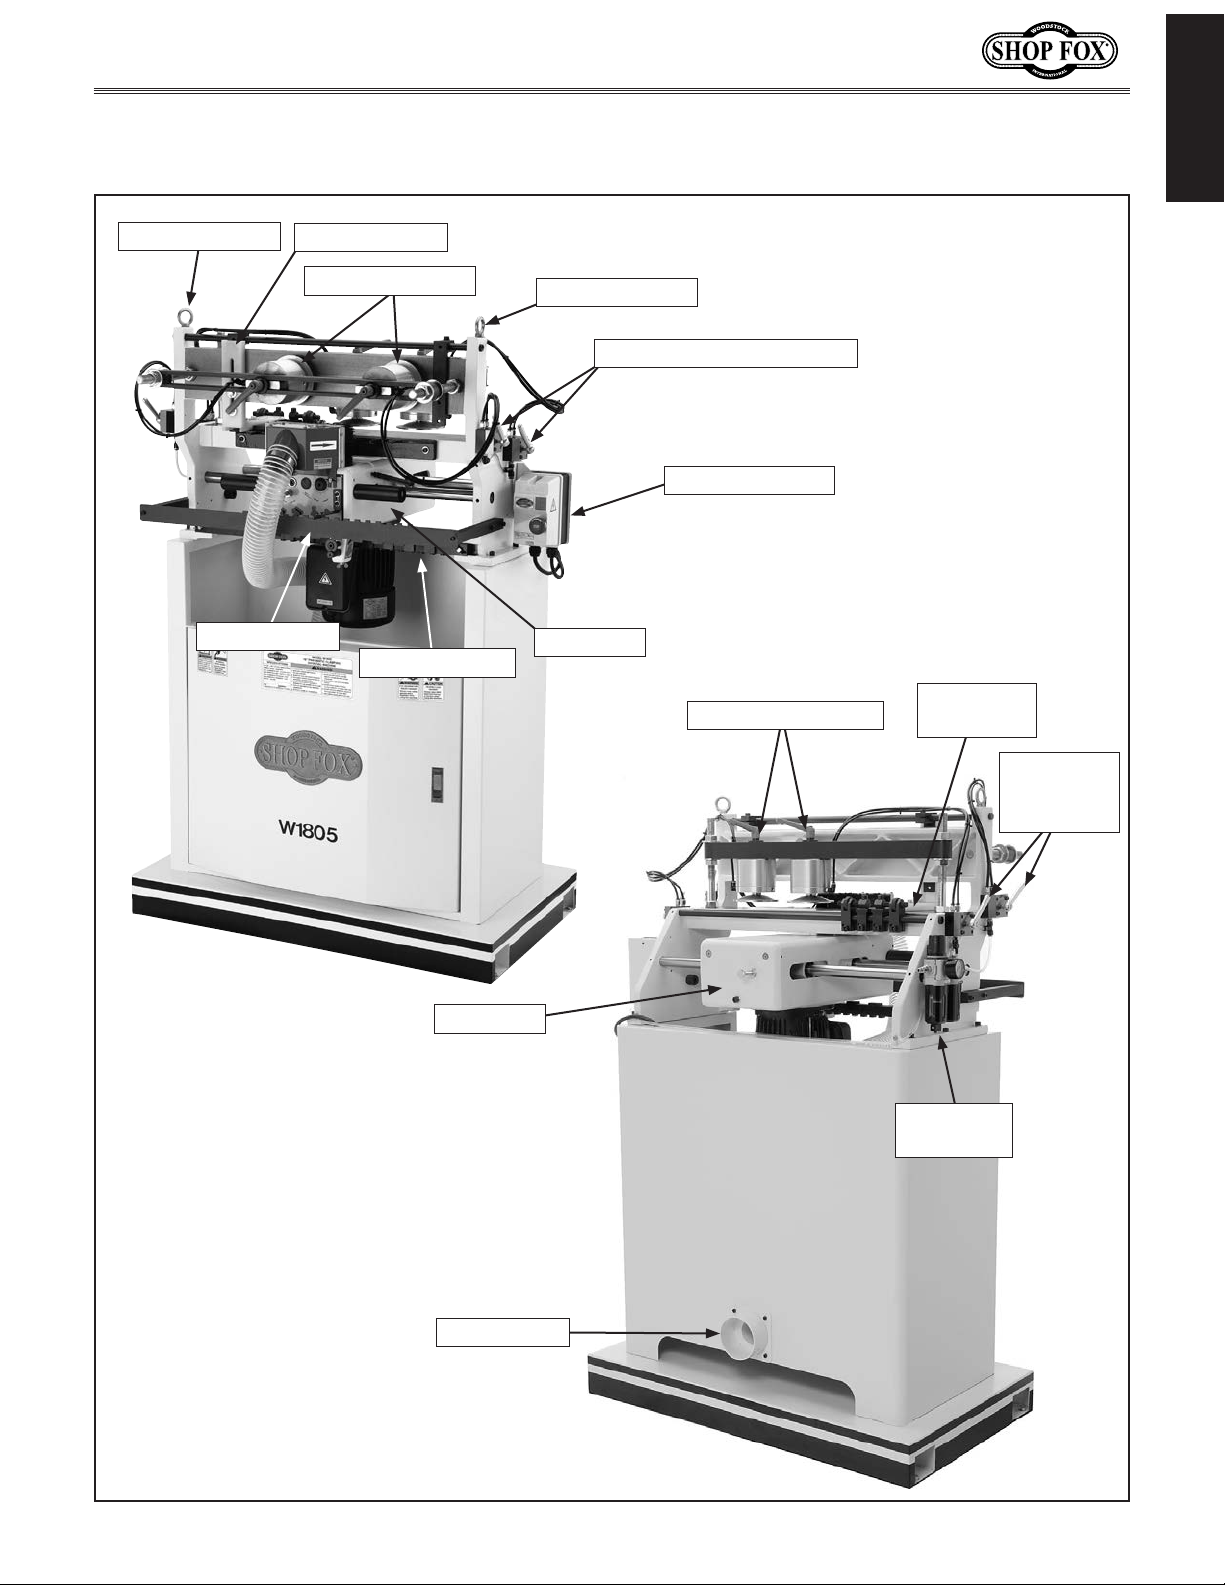
Controls & Features
INTRODUCTION
Lifting Eye Bolt
Template Bar
Vertical Fence
Vertical Clamps
Indicator Plate
Lifting Eye Bolt
Clamp Activation Handles
Magnetic Switch
Headstock
Horizontal Clamps
Horizontal
Fence
Clamp
Activation
Handles
Headstock
4" Dust Port
Air Supply
Unit
-5-
Page 8
Model W1805 (For Machines Mfd. Since 7/15)
SAFETY
OWNER’S MANUAL.
TRAINED OPERATORS ONLY.
DANGEROUS ENVIRONMENTS.
MENTAL ALERTNESS REQUIRED.
electrical components or improperly grounded
manual uses a series of symbols and signal words intended to convey the level of importance of the
safety messages. The progression of symbols is described below. Remember that safety messages by
SAFETY
For Your Own Safety,
Read Manual Before Operating Machine
The purpose of safety symbols is to attract your attention to possible hazardous conditions. This
SAFETY
themselves do not eliminate danger and are not a substitute for proper accident prevention measures—this responsibility is ultimately up to the operator!
NOTICE
Standard Machinery Safety Instructions
Standard Machinery Safety Instructions
Indicates an imminently hazardous situation which, if not avoided,
WILL result in death or serious injury.
Indicates a potentially hazardous situation which, if not avoided,
COULD result in death or serious injury.
Indicates a potentially hazardous situation which, if not avoided,
MAY result in minor or moderate injury.
This symbol is used to alert the user to useful information about
proper operation of the equipment or a situation that may cause
damage to the machinery.
Read and understand this
owner’s manual BEFORE using machine.
have a higher risk of being hurt or killed. Only
allow trained/supervised people to use this
machine. When machine is not being used,
disconnect power, remove switch keys, or
lock-out machine to prevent unauthorized
use—especially around children. Make
workshop kid proof!
machinery in areas that are wet, cluttered,
or have poor lighting. Operating machinery
in these areas greatly increases the risk of
accidents and injury.
alertness is required for safe operation of
machinery. Never operate under the influence
of drugs or alcohol, when tired, or when
distracted.
Untrained operators
Do not use
Full mental
ELECTRICAL EQUIPMENT INJURY RISKS. You can
be shocked, burned, or killed by touching live
machinery. To reduce this risk, only allow an
electrician or qualified service personnel to
do electrical installation or repair work, and
always disconnect power before accessing or
exposing electrical equipment.
DISCONNECT POWER FIRST. Always disconnect
machine from power supply BEFORE making
adjustments, changing tooling, or servicing
machine. This eliminates the risk of injury
from unintended startup or contact with live
electrical components.
EYE PROTECTION. Always wear ANSI-approved
safety glasses or a face shield when operating
or observing machinery to reduce the risk of
eye injury or blindness from flying particles.
Everyday eyeglasses are not approved safety
glasses.
-6-
Page 9
Model W1805 (For Machines Mfd. Since 7/15)
WEARING PROPER APPAREL. Do not wear
HAZARDOUS
HEARING PROTECTION.
REMOVE ADJUSTING TOOLS.
INTENDED USAGE.
AWKWARD POSITIONS.
CHILDREN & BYSTANDERS.
GUARDS & COVERS.
FORCING MACHINERY. Do not force machine. It
will do the job safer and better at the rate for
loss of control. Before starting, verify machine
malfunction, leading to serious personal injury
from heated surfaces, high traffic areas, harsh
clothing, apparel, or jewelry that can become
entangled in moving parts. Always tie back
or cover long hair. Wear non-slip footwear to
avoid accidental slips, which could cause loss
of workpiece control.
DUST. Dust created while using
machinery may cause cancer, birth defects,
or long-term respiratory damage. Be aware of
dust hazards associated with each workpiece
material, and always wear a NIOSH-approved
respirator to reduce your risk.
Always wear hearing
protection when operating or observing
loud machinery. Extended exposure to this
noise without hearing protection can cause
permanent hearing loss.
machinery can become dangerous projectiles
upon startup. Never leave chuck keys,
wrenches, or any other tools on machine.
Always verify removal before starting!
intended purpose—never make modifications
without prior approval from Woodstock
International. Modifying machine or using
it differently than intended will void the
warranty and may result in malfunction or
mechanical failure that leads to serious
personal injury or death!
balance at all times when operating machine.
Do not overreach! Avoid awkward hand
positions that make workpiece control difficult
or increase the risk of accidental injury.
bystanders at a safe distance from the work
area. Stop using machine if they become a
distraction.
Only use machine for its
Tools left on
Keep proper footing and
Keep children and
which it was designed.
NEVER STAND ON MACHINE. Serious injury may
occur if machine is tipped or if the cutting
tool is unintentionally contacted.
STABLE MACHINE. Unexpected movement during
operation greatly increases risk of injury or
is stable and mobile base (if used) is locked.
USE RECOMMENDED ACCESSORIES. Consult
this owner’s manual or the manufacturer for
recommended accessories. Using improper
accessories will increase risk of serious injury.
UNATTENDED OPERATION. To reduce the risk
of accidental injury, turn machine OFF and
ensure all moving parts completely stop
before walking away. Never leave machine
running while unattended.
MAINTAIN WITH CARE. Follow all maintenance
instructions and lubrication schedules to
keep machine in good working condition. A
machine that is improperly maintained could
or death.
CHECK DAMAGED PARTS. Regularly inspect
machine for any condition that may affect
safe operation. Immediately repair or replace
damaged or mis-adjusted parts before
operating machine.
MAINTAIN POWER CORDS. When disconnecting
cord-connected machines from power, grab
and pull the plug—NOT the cord. Pulling the
cord may damage the wires inside, resulting
in a short. Do not handle cord/plug with wet
hands. Avoid cord damage by keeping it away
chemicals, and wet/damp locations.
SAFETY
accidental contact with moving parts or flying
debris—make sure they are properly installed,
undamaged, and working correctly.
Guards and covers reduce
EXPERIENCING DIFFICULTIES. If at any time
you experience difficulties performing the
intended operation, stop using the machine!
-7-
Contact Technical Support at (360) 734-3482.
Page 10
Model W1805 (For Machines Mfd. Since 7/15)
Additional Safety for Dovetail Machines
READ and understand this
entire instruction manual
before using this machine.
SAFETY
GUARD. The guard helps protect the operator
from the spinning cutter and flying debris
during operation. Never operate the dovetail
machine or allow it to be connected to
power when the guard is removed or serious
personal injury may occur.
BOARD EJECTION. The machine may eject
boards in the horizontal position if they are
not clamped securely. Never allow others to
stand directly behind the dovetail machine
during operation or serious injury may occur.
SAFETY GLASSES. Even with the guard in
place, occasional chips may be ejected from
the machine. Operator and bystanders MUST
wear ANSI approved safety glasses to prevent
eye injuries.
CUTTER STARTING POSITION. Starting the
machine with the cutter against a workpiece
or fence may eject debris from the machine
and most likely will ruin the workpiece or
cutter. Move the cutter clear of any contact
before starting the machine!
Serious personal injury
may occur if safety and
operational information is
not understood and followed. DO NOT risk your
safety by not reading!
USE this and other machinery with caution
and respect. Always consider safety first,
as it applies to your individual working
conditions. No list of safety guidelines can
be complete—every shop environment is
different. Failure to follow guidelines could
result in serious personal injury, damage
to equipment or poor work results.
LOOSE CUTTER. Starting the machine with a
loose cutter may eject the cutter from the
machine at a high rate of speed, causing
serious personal injury to the operator or
bystanders. Always double-check that the
cutter is tight after adjusting.
REMOVE ADJUSTMENT TOOLS. Starting the
machine with a wrench left in the spindle
adjustment screw can result in serious
personal injury. Always remove any wrenches
or other adjustment tools from the machine
after adjustments have been made and
before starting the machine.
DUST COLLECTION. Using dust collection when
operating this machine greatly reduces flying
debris and fine airborne dust, which reduces
the risk of personal injury from these
hazards. Always use a dust collection system
when operating this machine.
DISCONNECT POWER BEFORE ANY
ADJUSTMENTS. This machine requires the
operator to work near the exposed cutter
during setup. Always disconnect power
BEFORE making adjustments to the machine
or serious personal injury may occur.
-8-
Page 11
Model W1805 (For Machines Mfd. Since 7/15)
This machine must be connected to the correct size and
type of power supply circuit, or fire or electrical damage
may occur. Read through this section to determine if an
adequate power supply circuit is available. If a correct
circuit is not available, a qualified electrician MUST install
one before you can connect the machine to power.
A power supply circuit includes all electrical equipment
between the breaker box or fuse panel in the building
and the machine. The power supply circuit used for
this machine must be sized to safely handle the fullload current drawn from the machine for an extended
period of time. (If this machine is connected to a circuit
protected by fuses, use a time delay fuse marked D.)
The full-load current rating is the amperage a machine
draws at 100% of the rated output power. On machines
with multiple motors, this is the amperage drawn by the
largest motor or sum of all motors and electrical devices
that might operate at one time during normal operations.
or machine damage. To reduce this risk,
where only one machine will be running
multiple machines will be running at the
This machine is prewired to operate on a power supply
circuit that has a verified ground and meets the following
requirements:
ELECTRICAL
Circuit Requirements
The machine must be properly set up
before it is safe to operate. DO NOT
connect this machine to the power
source until instructed to do so later
in this manual.
ELECTRICAL
Full-Load Current Rating
Full-Load Current Rating at 220V ....................5 Amps
Full-Load Current Rating at 110V .................. 10 Amps
Circuit Requirements for 220V (Prewired)
Nominal Voltage ................. 208V, 220V, 230V, 240V
Cycle ........................................................60 Hz
Phase .................................................... 1-Phase
Power Supply Circuit ................................ 15 Amps
Plug/Receptacle ................................... NEMA 6-15
Cord .................
Circuit Requirements for 110V
This machine can be converted to operate on a power
supply circuit that has a verified ground and meets the
requirements listed below. (Refer to 110V Wiring Diagram
on Page 34 for details.)
Circuit Type ............... 110V/120V, 60 Hz, Single-Phase
Circuit Size ............................................. 15 Amps
Plug/Receptacle .................................... NEMA 5-15
“S”-Type, 3-Wire, 14 AWG, 300 VAC
Incorrectly wiring or grounding this
machine can cause electrocution, fire,
only an electrician or qualified service
personnel should do any required
electrical work on this machine.
NOTICE
The circuit requirements listed in this
manual apply to a dedicated circuit—
at a time. If this machine will be
connected to a shared circuit where
same time, consult with an electrician
to ensure that the circuit is properly
sized for safe operation.
-9-
Page 12
Grounding Requirements
This machine MUST be grounded. In the event of certain
types of
a path of least resistance for electric current
order
Improper connection of the equipment-grounding
will
increase
insulation
grounding
cord or plug is necessary, do not connect the equipmentgrounding
Check with a qualified electrician or service personnel
if
or if
properly grounded.
plug is damaged or worn, disconnect it from power, and
immediately replace it with a new one.
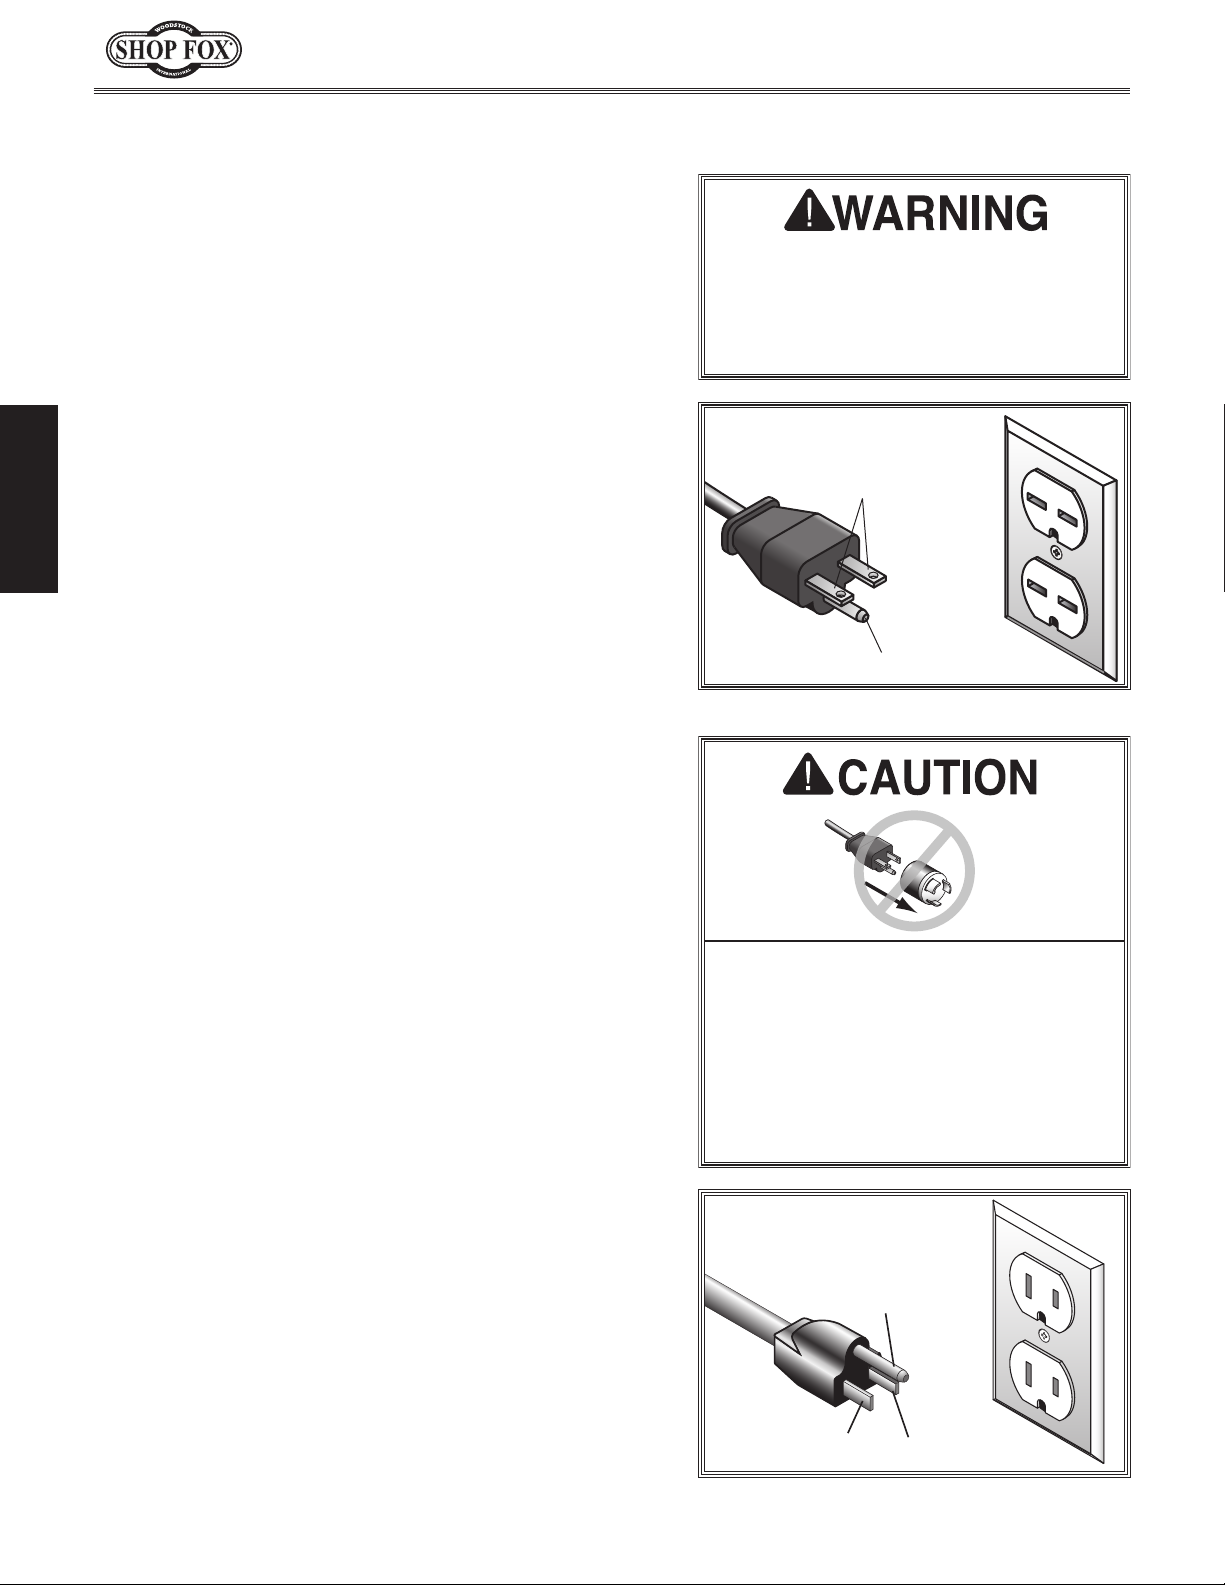
A NEMA 5-15 plug has a grounding prong that must be
attached to the equipment-grounding wire inside the
included power cord.
into a matching
installed and grounded in accordance with all local codes
and ordinances.
We do not recommend using an extension cord with
Any extension cord used with this machine must contain a
plug and receptacle, and
meet the following requirements:
the available receptacle or the machine
The power cord and plug specified under “Circuit
Requirements for 220V” on the previous page has an
equipment-grounding wire and a grounding prong. The
plug must only be inserted into a matching receptacle
(outlet) that is properly installed and grounded in
accordance with all local codes and ordinances (see
malfunctions or breakdowns, grounding provides
to travel—in
to reduce the risk of electric shock.
wire
the risk of electric shock. The wire with green
(with/without yellow stripes) is the equipment-
wire. If repair or replacement of the power
Model W1805 (For Machines Mfd. Since 7/15)
The machine must be properly set up
before it is safe to operate. DO NOT
connect this machine to the power
source until instructed to do so later
in this manual.
wire to a live (current carrying) terminal.
you do not understand these grounding requirements,
ELECTRICAL
you are in doubt about whether the tool is
If you ever notice that a cord or
For 220V Connection (Prewired)
For 110V Connection (Must be Rewired)
The plug must only be inserted
receptacle (see Figure) that is properly
this machine. Extension cords cause voltage drop, which
may damage electrical components and shorten motor
life. Voltage drop increases with longer extension cords
and smaller gauge sizes (higher gauge numbers indicate
smaller sizes).
ground wire, match the required
Minimum Gauge Size at 220V ...................... 14 AWG
Maximum Length (Shorter is Better) ................50 ft.
Extension Cords
-10-
220V
Current Carrying Prongs
6-15 PLUG
Figure 1. NEMA 6-15 plug & receptacle.
No adapter should be used with the
required plug. If the plug does not fit
must be reconnected to a different
type of circuit, the reconnection must
be made by an electrician or qualified
service personnel and it must comply
with all local codes and ordinances.
110V
5-15 PLUG
Figure 2. NEMA 5-15 plug & receptacle.
GROUNDED
6-15 RECEPTACLE
Grounding Pin
GROUNDED
5-15 RECEPTACLE
Grounding Pin
Neutral Hot
Page 13
Model W1805 (For Machines Mfd. Since 7/15)
This machine has been carefully packaged for safe
transportation. If you notice the machine has been
damaged during shipping, please contact your authorized
Shop Fox dealer immediately.
SETUP
Unpacking
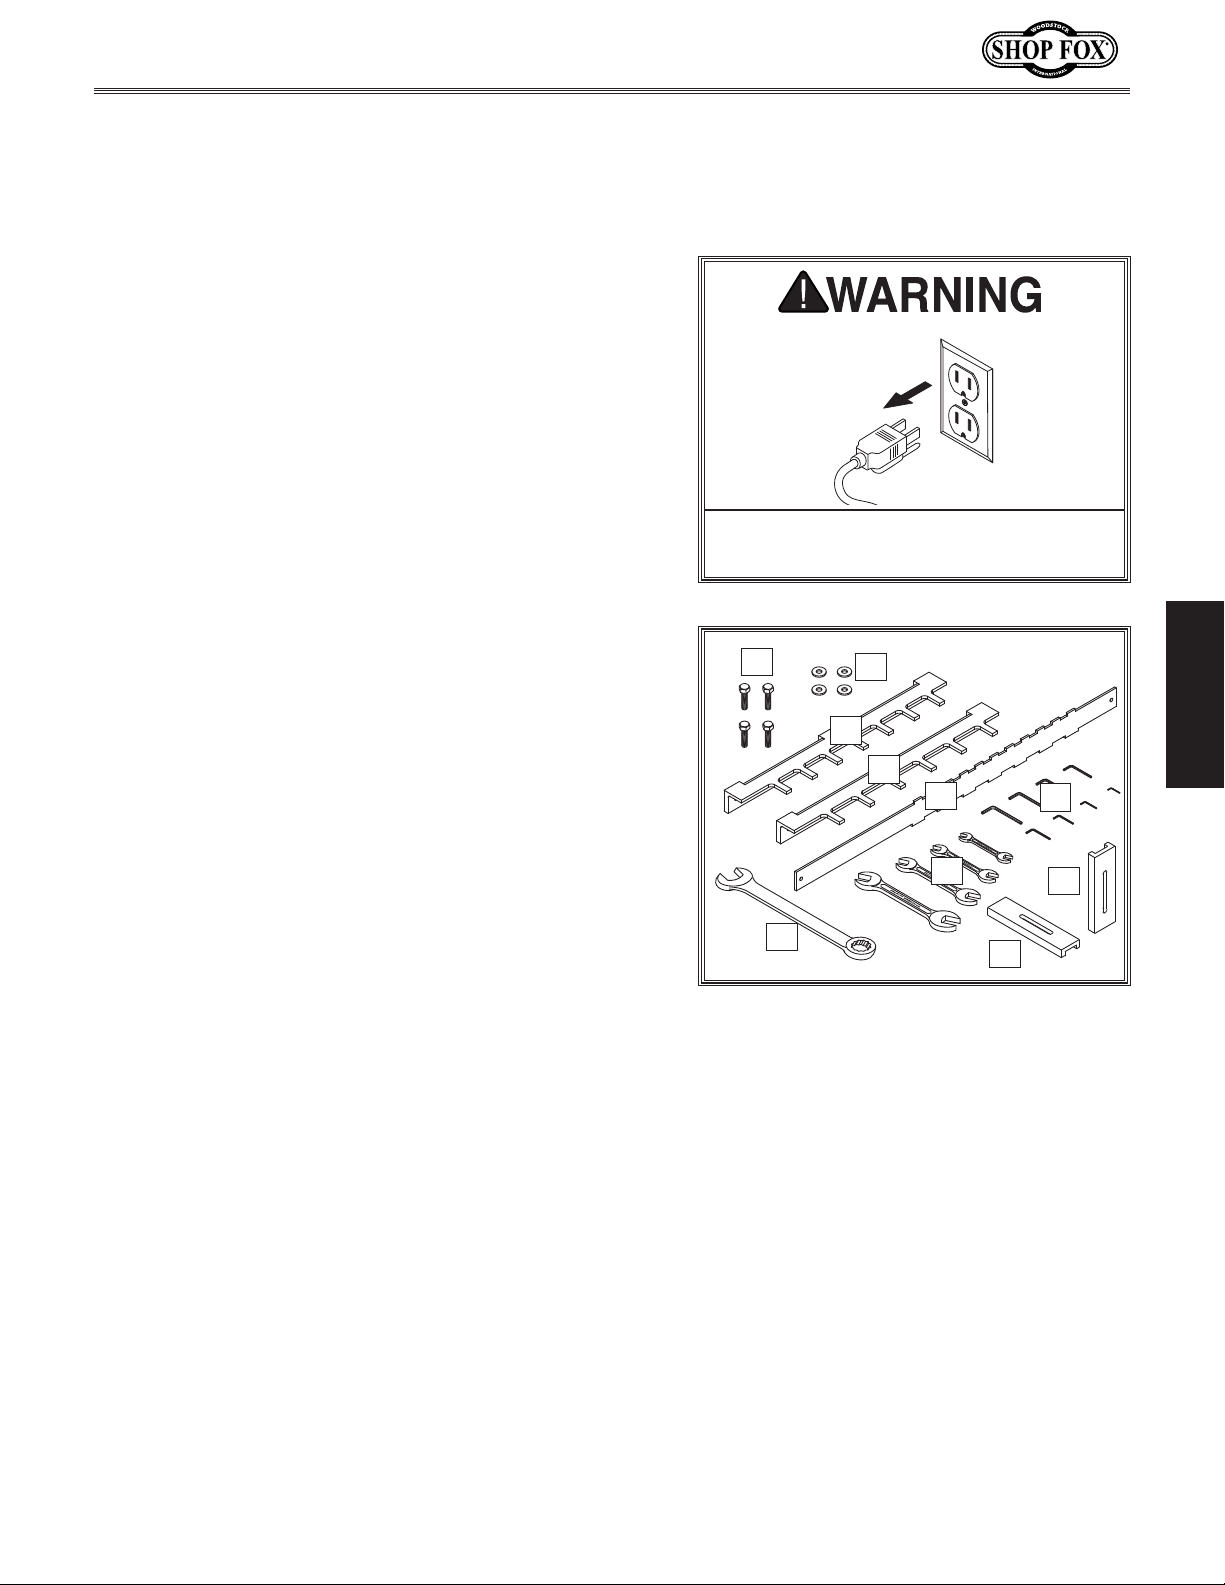
Inventory
The following is a description of the main components
shipped with the Model W1805. Lay the components out
to inventory them.
Note: If you can't find an item on this list, check the
mounting location on the machine or examine the
packaging materials carefully. Occasionally we pre-install
certain components for safer shipping.
Keep machine disconnected from
power until instructed otherwise.
A
B
SETUP
Box Inventory: (Figure 3) Qty
A. Hex Bolts M8-1.25 x 20 ...................................4
Flat Washers 8mm .........................................4
B.
Fixed Chaser 21⁄2" .........................................1
C.
Fixed Chaser 3" ............................................1
D.
Indicator Bar 11⁄2" and 21⁄2" .............................1
E.
Hex Wrench Set
F.
(1.5-6mm) ........................................... 1 Each
Combo Wrench Set
G.
(8-10, 11-13, 12-14, and 17-19mm) ............. 1 Each
Extra Vertical HDPE Fence ...............................1
H.
Extra Horizontal HDPE Fence ............................1
I.
Open-End Offset Wrench 30mm .........................1
J.
C
D
E
G
J
Figure 3. Model W1805 inventory.
F
H
I
-11-
Page 14
Model W1805 (For Machines Mfd. Since 7/15)
The unpainted surfaces of your machine are
coated with a heavy-duty rust preventative that
prevents corrosion during shipment and storage.
This rust preventative works extremely well, but
it will take a little time to clean.
Be patient and do a thorough job cleaning your
machine. The time you spend doing this now will
give you a better appreciation for the proper
care of your machine's unpainted surfaces.
There are many ways to remove this rust
preventative, but the following steps work well
in a wide variety of situations. Always follow the
manufacturer’s instructions with any cleaning
product you use and make sure you work in a
well-ventilated area to minimize exposure to
toxic fumes.
Before cleaning, gather the following:
• Disposable rags
• Cleaner/degreaser (WD•40 works well)
• Safety glasses & disposable gloves
• Plastic paint scraper (optional)
Basic steps for removing rust preventative:
1. Put on safety glasses.
2. Coat the rust preventative with a liberal
amount of cleaner/degreaser, then let it
soak for 5–10 minutes.
3. Wipe off the surfaces. If your cleaner/
degreaser is effective, the rust
preventative will wipe off easily. If you
have a plastic paint scraper, scrape off as
much as you can first, then wipe off the
rest with the rag.
4. Repeat Steps 2–3 as necessary until clean,
then coat all unpainted surfaces with a
quality metal protectant to prevent rust.
Avoid chlorine-based solvents, such as
acetone or brake parts cleaner, that may
damage painted surfaces.
Machine Placement
• Floor Load: This machine distributes a
heavy load in a small footprint. Some
residential floors may require additional
SETUP
bracing to support both machine and
operator.
• Working Clearances: Consider existing and
anticipated needs, size of material to be
processed through the machine, and space
for auxiliary stands, work tables or other
machinery when establishing a location for
your machine.
• Lighting: Lighting should be bright enough
to eliminate shadow and prevent eye strain.
• Electrical: Electrical circuits must be
dedicated or large enough to handle
amperage requirements. Outlets must be
located near each machine, so power or
extension cords are clear of high-traffic
areas. Follow local electrical codes for
proper installation of new lighting, outlets,
or circuits.
USE helpers or power lifting equipment to lift this
161⁄2" Dovetail Machine.
Otherwise, serious personal injury may occur.
Cleaning Machine
MAKE your shop “child
safe.” Ensure that your
workplace is inaccessible
to children by closing and
locking all entrances when
you are away. NEVER allow
untrained visitors in your
shop when assembling,
adjusting or operating
equipment.
-12-
Page 15
Model W1805 (For Machines Mfd. Since 7/15)
Lifting & Moving
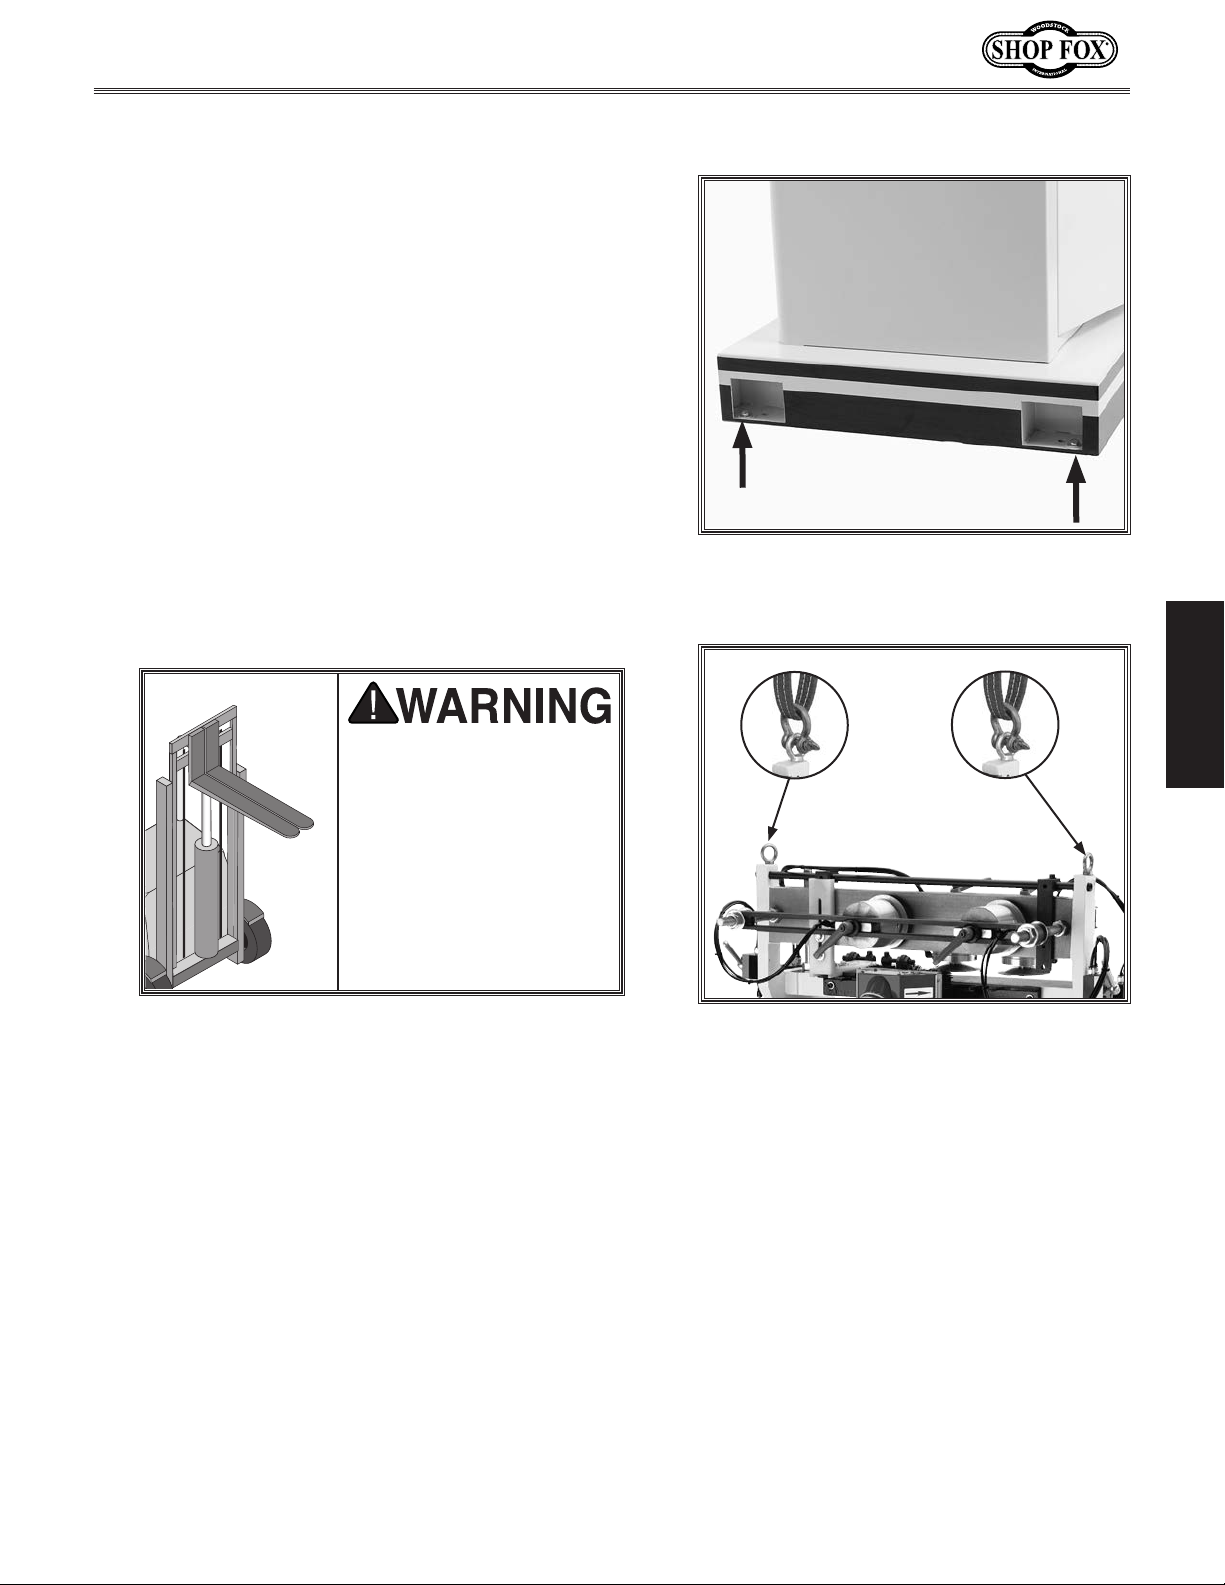
The Model W1805 is designed to be lifted from two eye
bolts mounted near the top of the machine, on both
sides, using a forklift with lifting straps. The lifting straps
can be connected to the eye bolts with metal shackles.
To lift the Model W1805 with a forklift, do these steps:
1. Unbolt the base of the dovetail machine from the
shipping pallet (
placement.
Connect the lifting straps to the eye bolts, using
2.
shackles, as shown in Figure 5.
Lift the machine and place it in your desired
3.
location.
Remove the forklift straps.
4.
Figure 4), so it can be removed for
Figure 4. Example of where machine is
bolted to the pallet (shows only one side;
machine is also bolted on other side).
SETUP
The Model W1805 is a
heavy machine. Serious
personal injury may occur
if safe moving methods are not used. To be
safe, get assistance and
use power equipment to
move the shipping crate
and remove the machine
from the crate.
Figure 5. Lifting machine from eyes.
-13-
Page 16
Mounting to Shop Floor
Although not required, we recommend mounting your new
machine to the floor. Since this is an optional step and
floor materials may vary, floor mounting hardware is not
included.
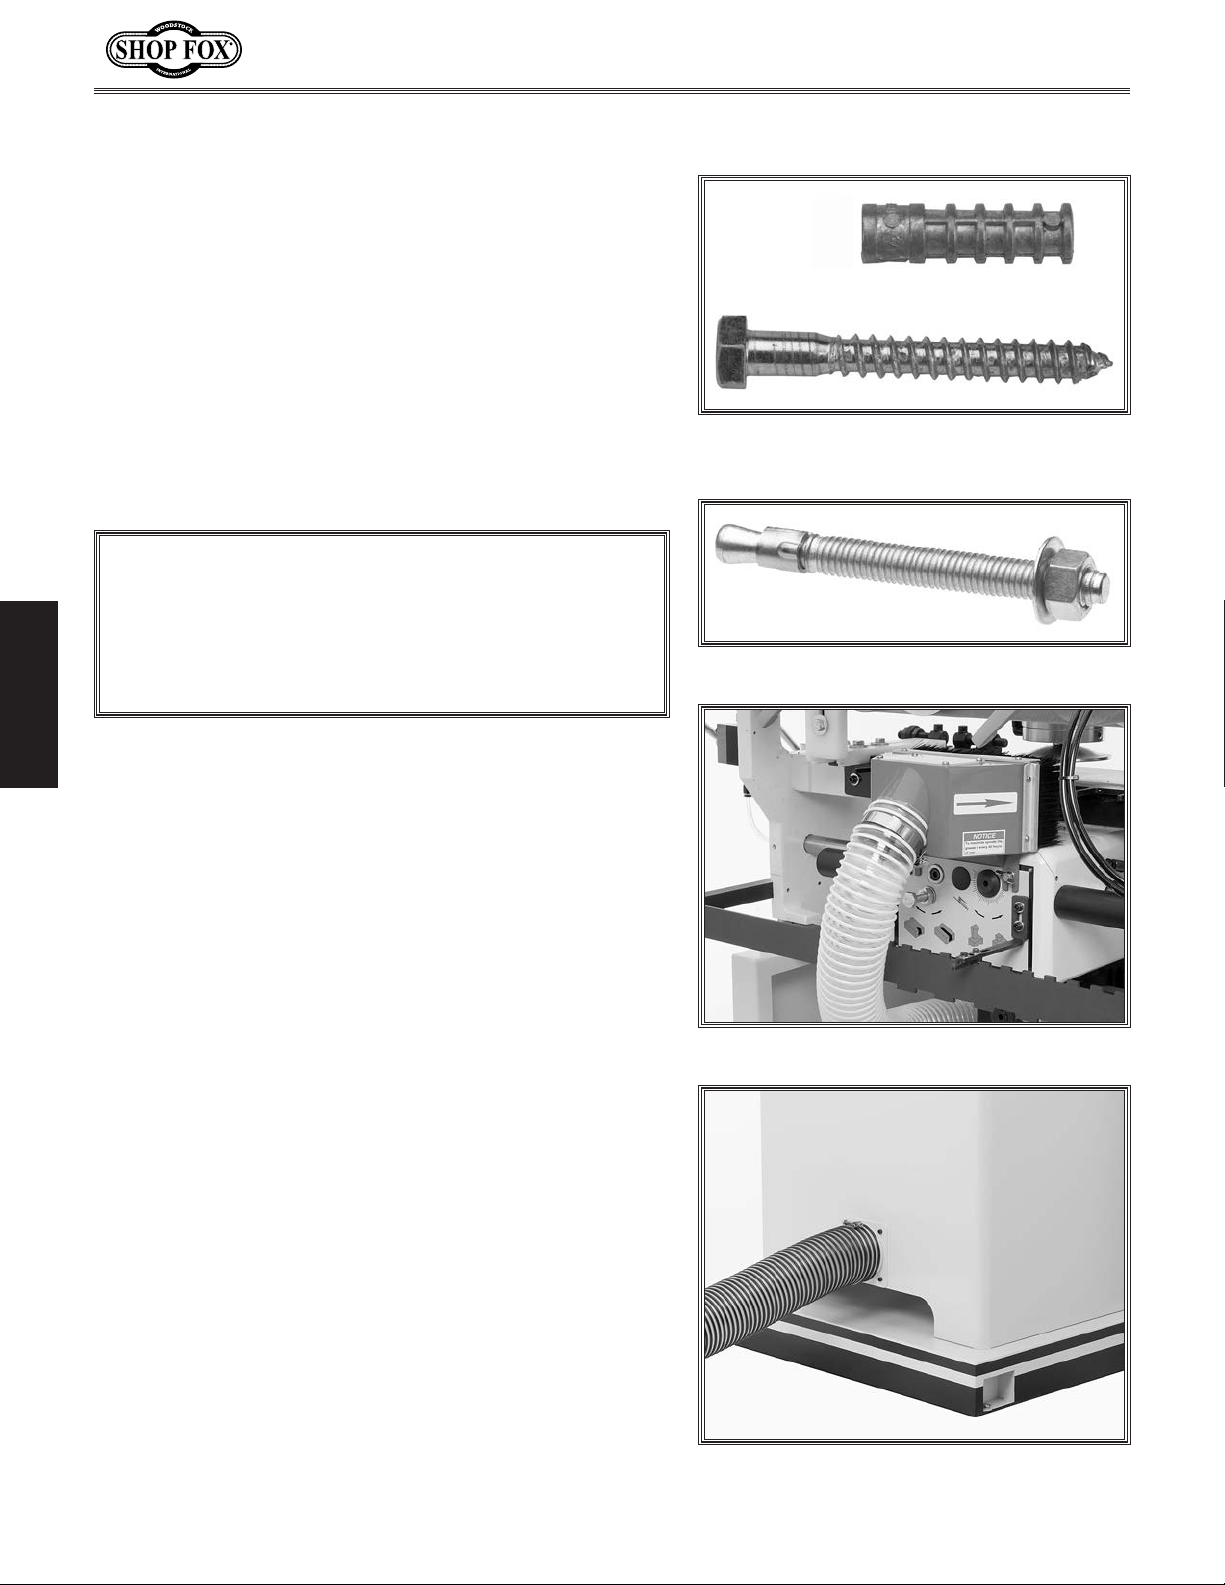
Bolting to Concrete Floors
Lag shield anchors used with lag bolts (Figure 6) and
anchor studs (
anchoring an object to a concrete floor. We suggest you
research the many options and methods for mounting
your machine and choose the best that fits your specific
application.
Figure 7) are two popular choices for
NOTICE
Anchor studs are stronger and more permanent
alternatives to lag shield anchors; however, they will
stick out of floor, which may cause a tripping hazard
if you decide to move your machine at a later point.
Model W1805 (For Machines Mfd. Since 7/15)
Figure 6. Typical lag shield anchor and lag
bolt.
Figure 7. Typical anchor stud.
SETUP
Assembly
To assemble the dovetail machine, attach the dust hose
to the guard, as shown in
Figure 8.
Dust Collection
Attach the dust port to your dust collection system with a
4" hose, as shown in
Recommended CFM at Dust Port: ................ 400 CFM
Do not confuse this CFM recommendation with the rating
of the dust collector. To determine the CFM at the
dust port, you must take into account many variables,
including the CFM rating of the dust collector, the length
of hose between the dust collector and the machine, the
amount of branches or Y's, and the amount of other open
lines throughout the system. Explaining this calculation
is beyond the scope of this manual. If you are unsure of
your system, consult an expert or purchase a good dust
collection "how-to" book.
Figure 9.
Figure 8. Dust hose attached to guard.
-14-
Figure 9. Dust collection hose attached to
dust port.
Page 17
Model W1805 (For Machines Mfd. Since 7/15)
Air Connection
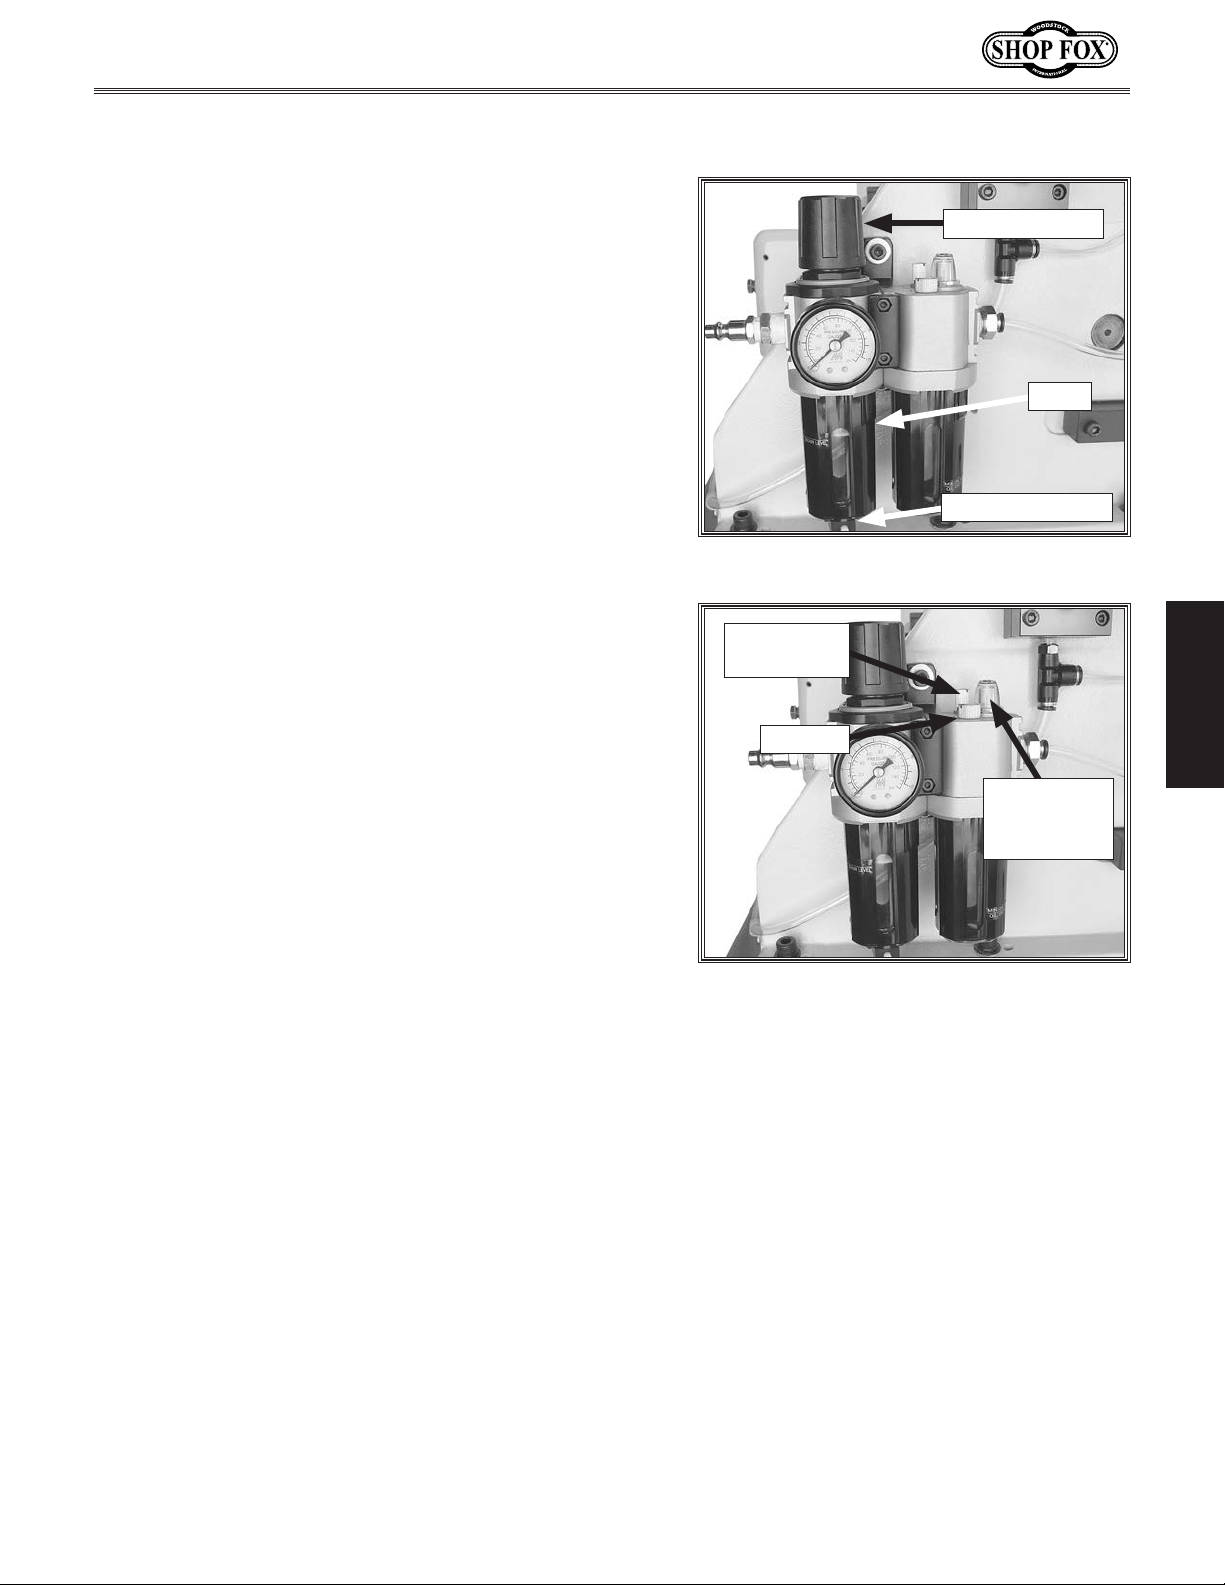
The air supply unit features a regulator, a filter, and a
lubricator (
must be setup properly before operating the machine.
To prepare the air supply unit for operation, do these
steps:
Connect your air hose to the air supply unit with a
1.
standard 1⁄4" NPT female quick-release coupler.
— If air leaks from the bottom of the filter, the
Check the air pressure reading on the gauge. The
2.
correct setting is 40 psi.
Figure 10 & 11). Each of these components
filter drain plug may be in "drain" mode. Move
the adjustment at the bottom of the filter to the
other side to put it in "plug" mode.
Regulator Knob
Filter
Filter Drain Plug
Figure 10. Air regulator and filter
— If the setting is correct, skip to Step 4.
— If the setting is not correct, proceed to the next
step.
Pull up on the regulator knob, rotate it in the
3.
direction necessary until the gauge reads 40 psi,
then push the knob down to lock it.
Adjust the lubricator by turning the lubrication
4.
dial clockwise until it stops, then turning it
counterclockwise one full turn. (Further adjustments
can be made later as necessary.)
Lubrication
Rate Dial
Fill Plug
Lubrication
Rate
Window
Figure 11. Air lubricator features.
SETUP
-15-
Page 18
Test Run
Once the assembly is complete, test run your machine to
make sure it runs properly and is ready for operation.
The test run consists of verifying the following: 1) The
motor powers up and runs correctly, 2) the motor turns the
correct direction (the motor included with this machine is
bi-directional), and 3) the safety disabling mechanism on
the switch works correctly.
If, during the test run, you cannot easily locate the source
of an unusual noise or vibration, stop using the machine
immediately, then review Troubleshooting on
Page 36.
Model W1805 (For Machines Mfd. Since 7/15)
Projectiles thrown from the machine
could cause serious eye injury. Wear
safety glasses to reduce the risk of
injury.
To test run the machine, do these steps:
Make sure you have read the safety instructions at
1.
the beginning of the manual and that the machine is
setup properly.
Make sure all tools and objects used during setup are
2.
cleared away from the machine.
SETUP
Connect the machine to the power source.
3.
4. Push the stop button in, then twist it clockwise so it
pops out.
Verify that the machine is operating correctly by
5.
turning it ON.
— When operating correctly, the machine runs
smoothly with little or no vibration or rubbing
noises.
— Investigate and correct strange or unusual noises
or vibrations before operating the machine further.
Always disconnect the machine from power before
investigating or correcting potential problems.
Turn the machine OFF.
6.
Push the STOP button in to make sure it is NOT
7.
popped out.
Press the green ON button.
8.
—If the machine starts, immediately stop it.
The switch disabling feature is not working
correctly. This safety feature must work properly
before proceeding with regular operations. Call
Tech Support.
—If the machine does not start, the
switch disabling feature is working
as designed.
Verify that the cutter is turning the
9.
correct direction by starting the
motor, then stopping the motor while
watching the cutter through the guard
window.
— If the cutter turns counterclockwise,
it is turning in the correct direction.
Proceed to
— If the cutter turns clockwise, it
is turning in the wrong direction.
Contact our Technical Support for
help.
10. Test the clamps. The clamps should
clamp down when the switch is turned
ON and they should raise up when the
switch is turned OFF.
—If the clamps work as stated,
no additional adjustments are
necessary.
— If the clamps do not work as stated,
troubleshoot and correct the
clamping system. Contact Technical
Support for help.
Step 10.
-16-
Page 19
Model W1805 (For Machines Mfd. Since 7/15)
OPERATIONS
General
This machine will perform many types of operations
that are beyond the scope of this manual. Many of these
operations can be dangerous or deadly if performed incorrectly.
The instructions in this section are written with the understanding that the operator has the necessary knowledge
and skills to operate this machine.
experiencing difficulties performing any operation, stop
using the machine!
If you are an inexperienced operator, we strongly recommend that you read books, trade articles, or seek training
from an experienced dovetail machine operator before
performing any unfamiliar operations.
safety should come first!
If at any time you are
Above all, your
READ and understand this entire instruction manual before using this machine.
Serious personal injury may occur if
safety and operational information is not
understood and followed. DO NOT risk
your safety by not reading!
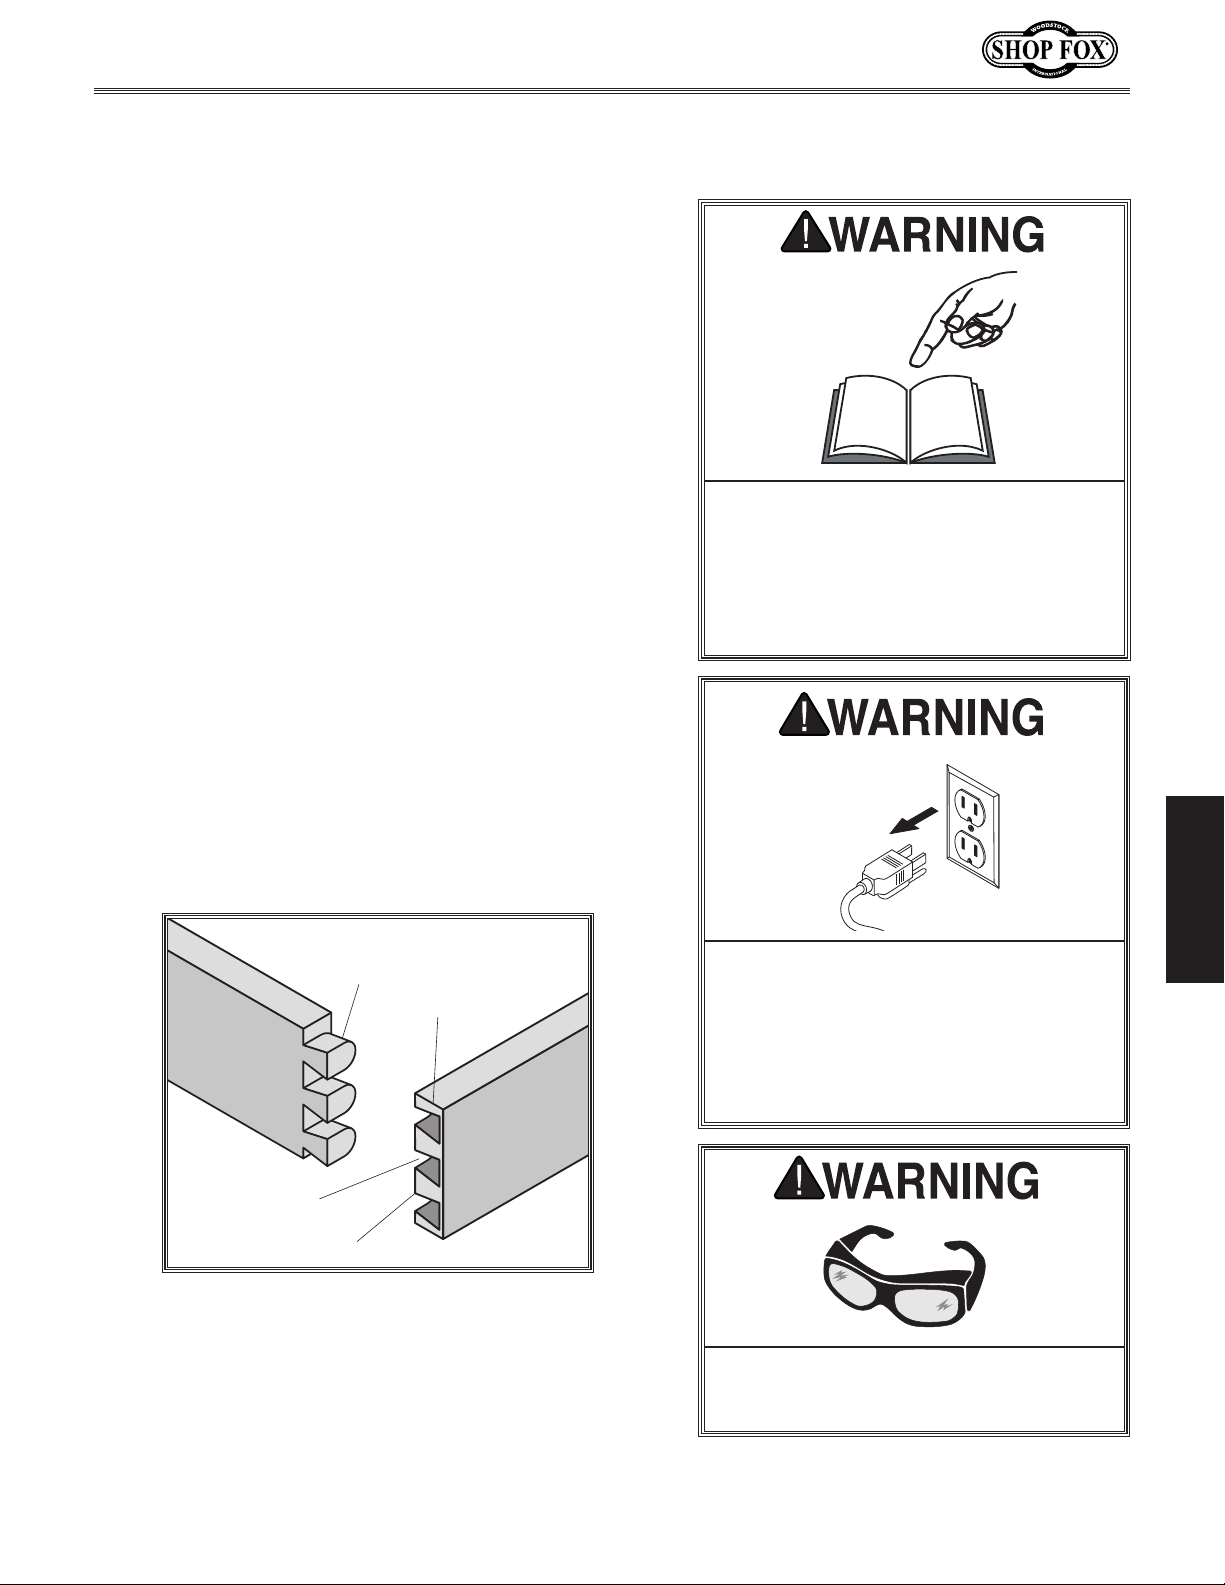
Dovetail Terminology
Take a moment to review the dovetail terminology shown
Figure 12. These terms will be used throughout this
in
section and knowing their meaning is important to fully
understand the controls of the machine.
Tail
Half Pin
Drawer
Side
Drawer
Front
Socket
Pin
Figure 12. Dovetail terminology.
OPERATIONS
DO NOT investigate problems or adjust
the machine while it is running. Wait
until the machine is turned OFF,
unplugged and all working parts
have come to a complete stop before
proceeding!
-17-
Always wear safety glasses when operating this machine. Failure to comply
may result in serious personal injury.
Page 20
Stock Preparation
Stock preparation is one of the most important steps for
cutting dovetails. Stock must be properly squared up or
the dovetails will not fit in the sockets tightly or evenly.
With proper planning and preparation, you can achieve
perfect results.
Stock Size
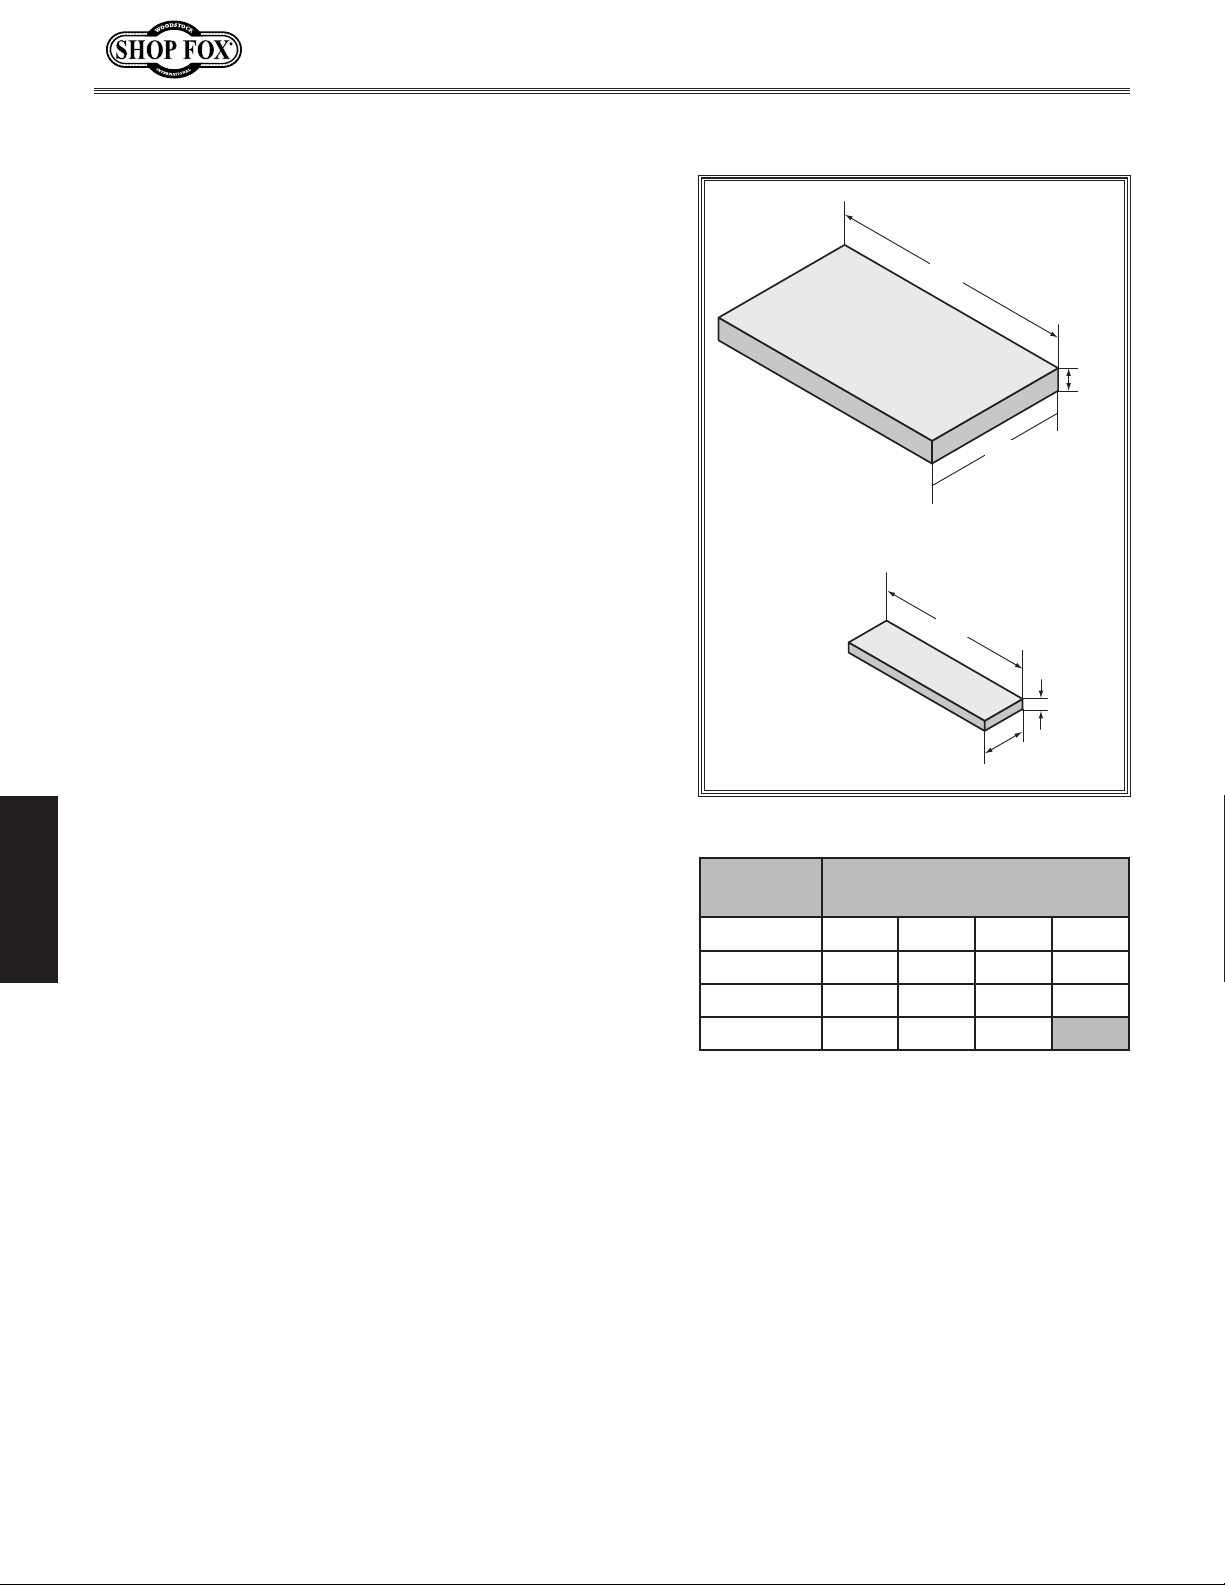
When selecting your stock, make sure that the stock size
is within the minimum and maximum dimensions that this
machine is capable of processing (see
The first consideration when preparing your stock is to
determine the width (height of drawer). The dovetail
machine includes a 4-sided template with the following
1
sizes: 1", 1
⁄2", 2", and 21⁄2".
Figure 13).
Model W1805 (For Machines Mfd. Since 7/15)
59"
23⁄8"
Maximum
161⁄2"
Stock Size
To achieve perfect dovetail spacing from edge-to-edge,
the stock width should be a multiple of the template size.
1
For example, when using a 1
1
should divisible by 1
⁄2". Refer to Figure 14 for more
⁄2" template, the stock width
examples.
Note: If you do not have control over the stock width, you
can still use the machine, but the half-pins on each edge
will not be the same size.
OPERATIONS
77⁄8"
13
Minimum
⁄32"
Stock Size
23⁄8"
Figure 13. Model W1805 stock size limits.
Template
Size
1"
1
1
⁄2" 41⁄2"
2"
1
2
⁄2"
Figure 14. Common width sizes used with
the available template sizes.
Common Stock Width used
with Template Sizes
3" 4" 5" 6"
6"
71⁄2"
9"
4" 6" 8" 10"
5"
71⁄2"
10"
-18-
Page 21
Model W1805 (For Machines Mfd. Since 7/15)
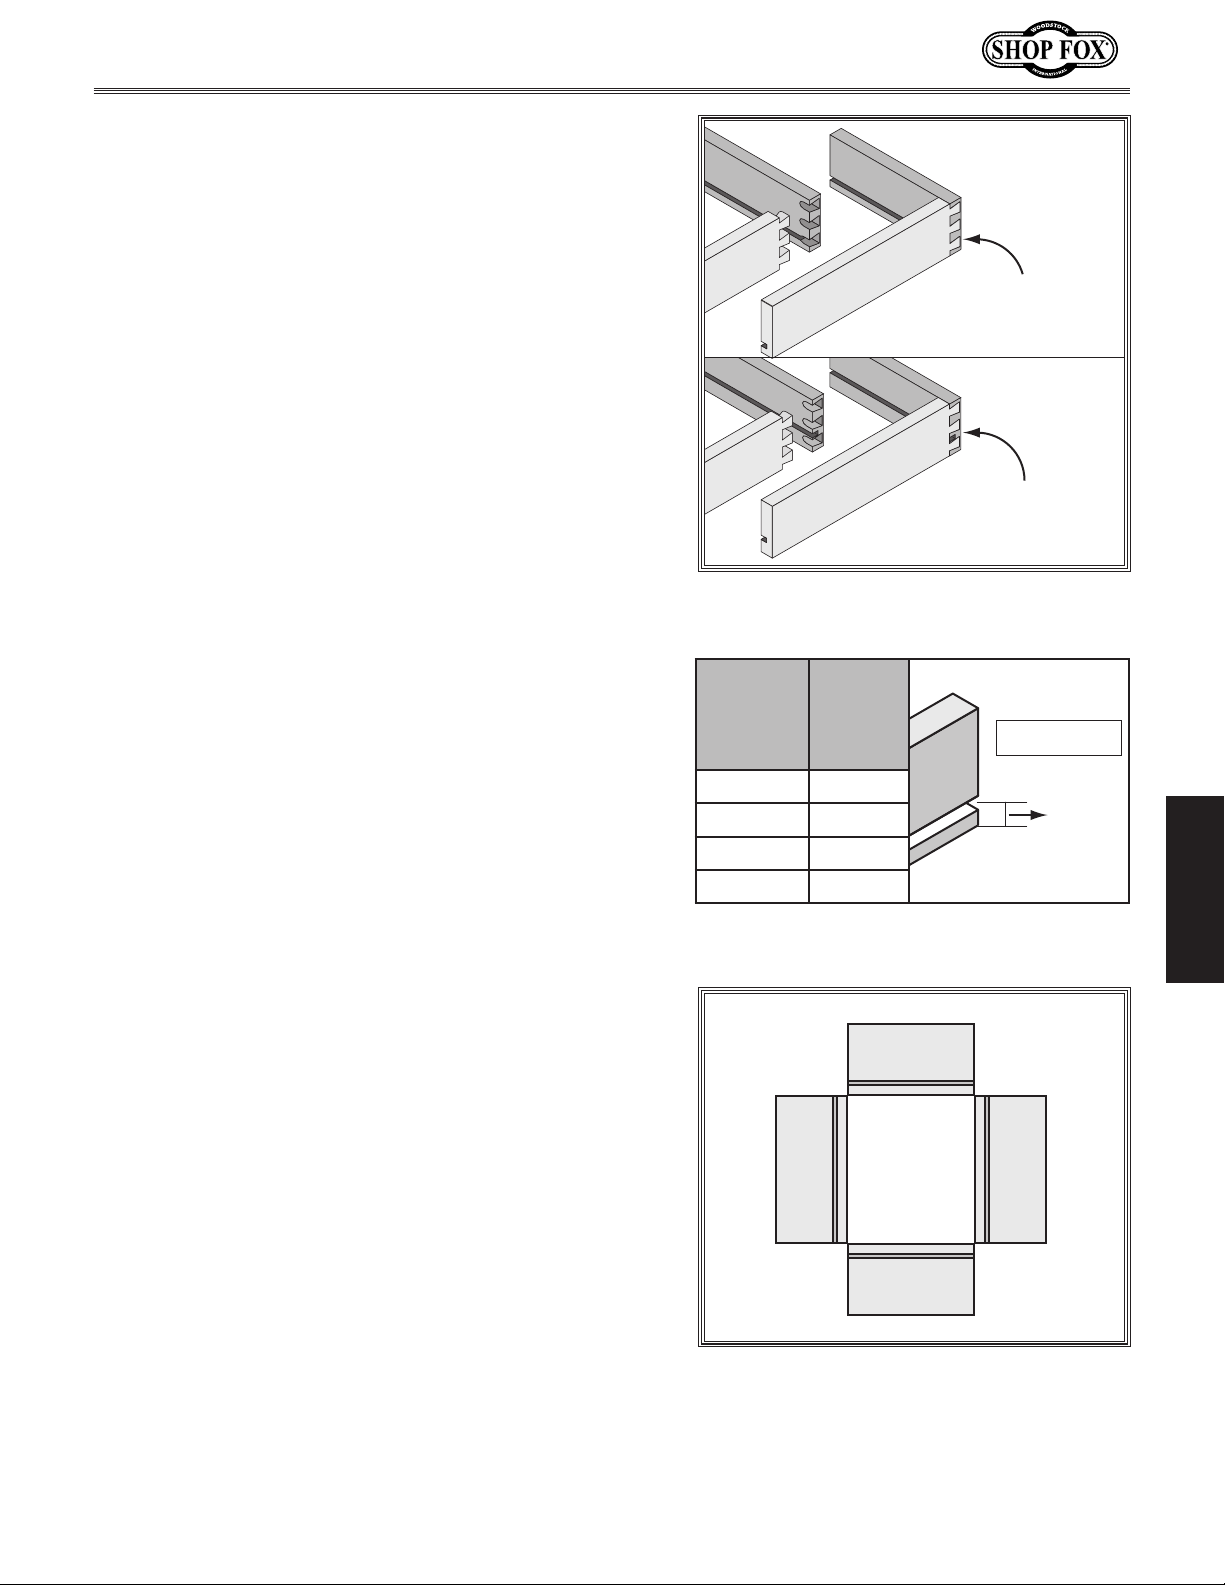
Dado Placement
The dado placement for a drawer bottom is dictated by
the size of template you use. In order for the dado to be
hidden when the dovetail joint is assembled, it must run
through a socket.
Figure 15 illustrates this concept.
CORRECT
A general rule of thumb: Cut the center of the dado half
the distance of the template size from the bottom edge
of the stock.
For example, when using a 1" template, center the dado
1
⁄2" from the bottom of all four pieces. This placement
ensures that the dado will end up in the first socket and
will not be visible when the drawer is assembled.
Figure
16 shows the ideal dado placement for each template
size.
Note: If your stock width is not a multiple of the
template size, this rule of thumb does not apply. Instead,
just cut the dado where you need it and center the socket
placement by eye when setting up the machine.
Dado is not
Visible
(Slot is Centered in Socket)
WRONG
Dado is Visible
(Slot is not Centered in Socket)
Figure 15. Correct dado placement so
dado is not visible after assembly.
Center
Template
Size
of Dado
from
Bottom
1"
1
1
⁄2"
2"
1
2
⁄2" 11⁄4"
1
3
⁄2"
⁄4"
1"
Figure 16. Dado placement for template
sizes.
EXAMPLE:
Stock
Dado Distance
from Bottom
1" Template
1
⁄2" on
Center
OPERATIONS
Layout
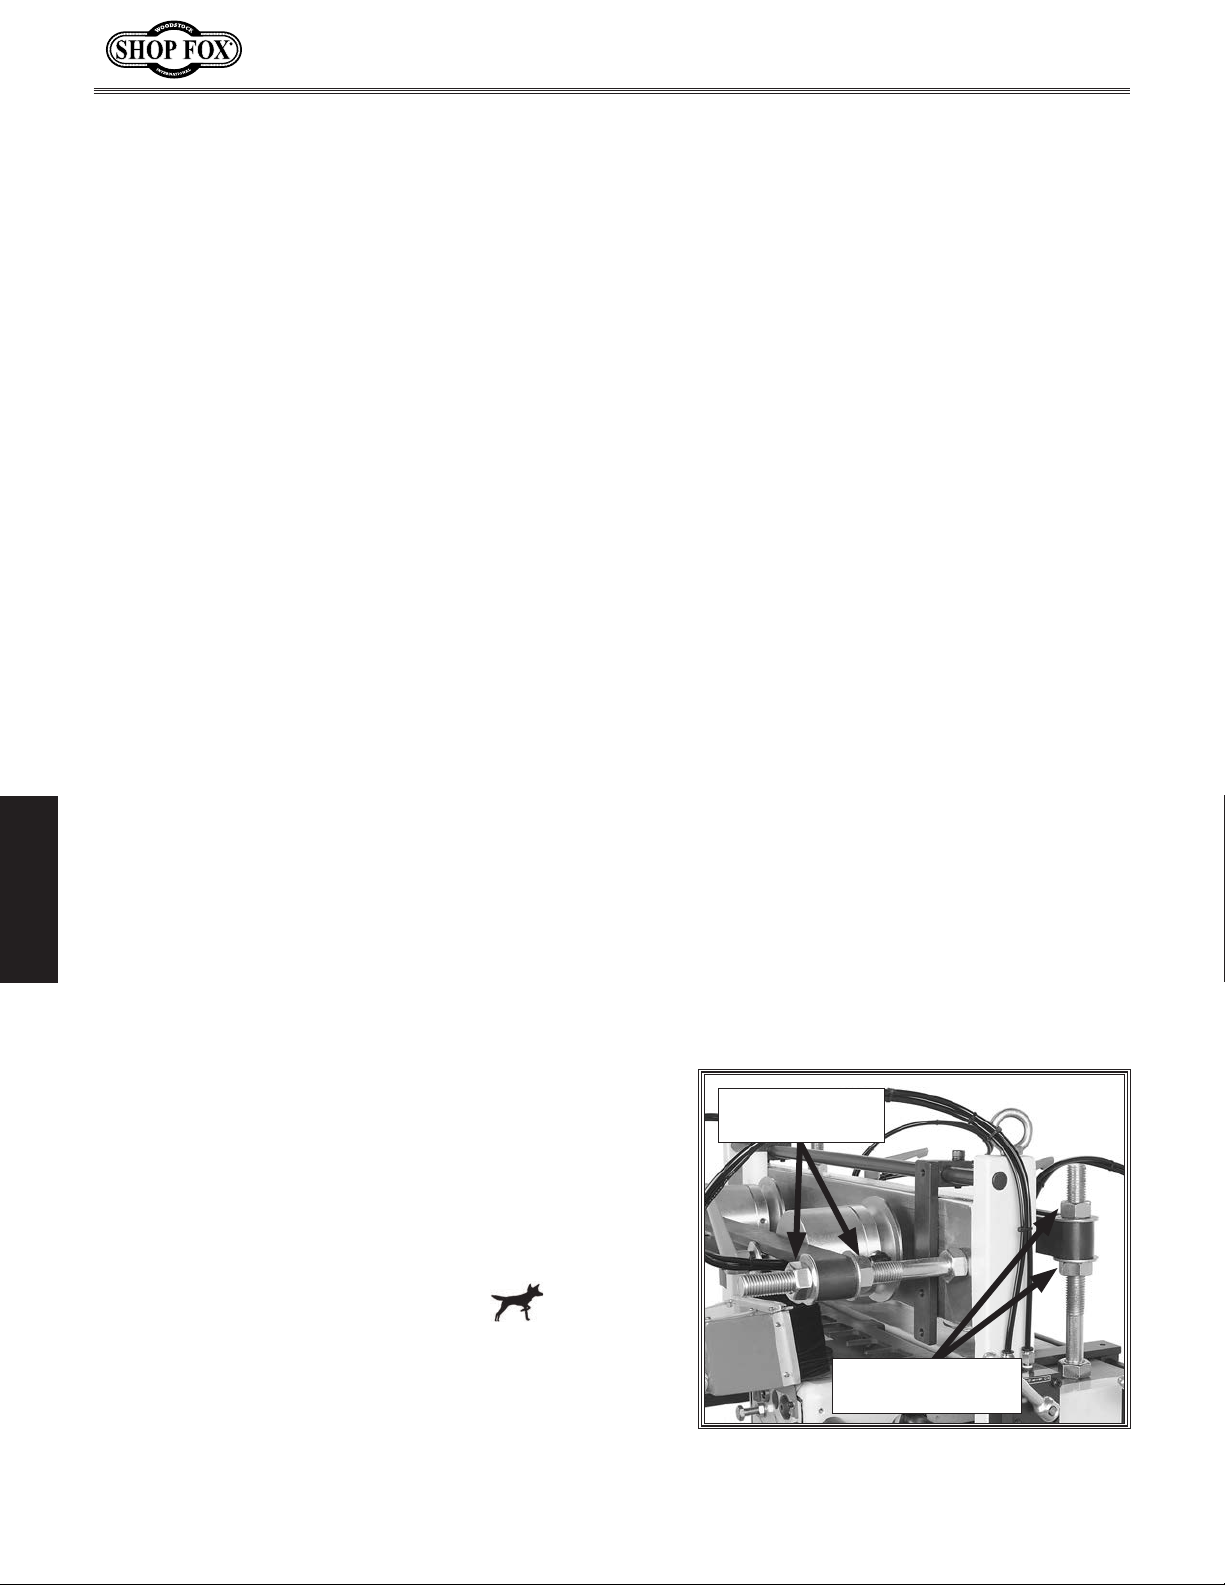
After you have dadoed and dimensioned your stock,
layout and mark the drawer pieces as shown in
This will help you keep track of the pieces as you cut the
dovetails.
Figure 17.
-19-
BACK
LEFT RIGHT
FRONT
Figure 17. Drawer pieces laid out and
marked; the inside of the drawer pieces
are face up.
Page 22
Dovetail Setup
Setting up the dovetail machine is a complex procedure
that involves trial-and-error and may take a fair amount of
time to complete.
Once you have the machine setup for a particular stock
size, you can repeat dovetails for that size indefinitely
without additional adjustments. However, if you change
stock size, then you must repeat this entire setup section.
Before starting any setup, you must prepare workpieces
for one drawer. These must be exactly the same size as
the drawers you will make during your production run.
Since trial-and-error is involved, this first drawer may end
up as scrap; therefore, do not prepare ALL the drawer
pieces for your production run until you have properly
setup the machine and have achieved satisfactory dovetail
joints on your test workpieces.
Model W1805 (For Machines Mfd. Since 7/15)
The setup procedures that follow refer to the drawer
pieces by their position during cutting. To avoid confusion
during the instructions, remember this:
Drawer Sides (L,R) = Vertical Workpiece
Drawer Front/Back (B, F) = Horizontal Workpiece
Follow the procedures in this section in order to properly
setup your machine for operation.
Setting Clamping Thickness
1. Check the current distance between the clamps and
OPERATIONS
the tables in relation to your workpiece thickness.
—If your workpiece fits between the clamps, then
further adjustments are not necessary.
—If your workpiece does not fit between the clamps,
then proceed to
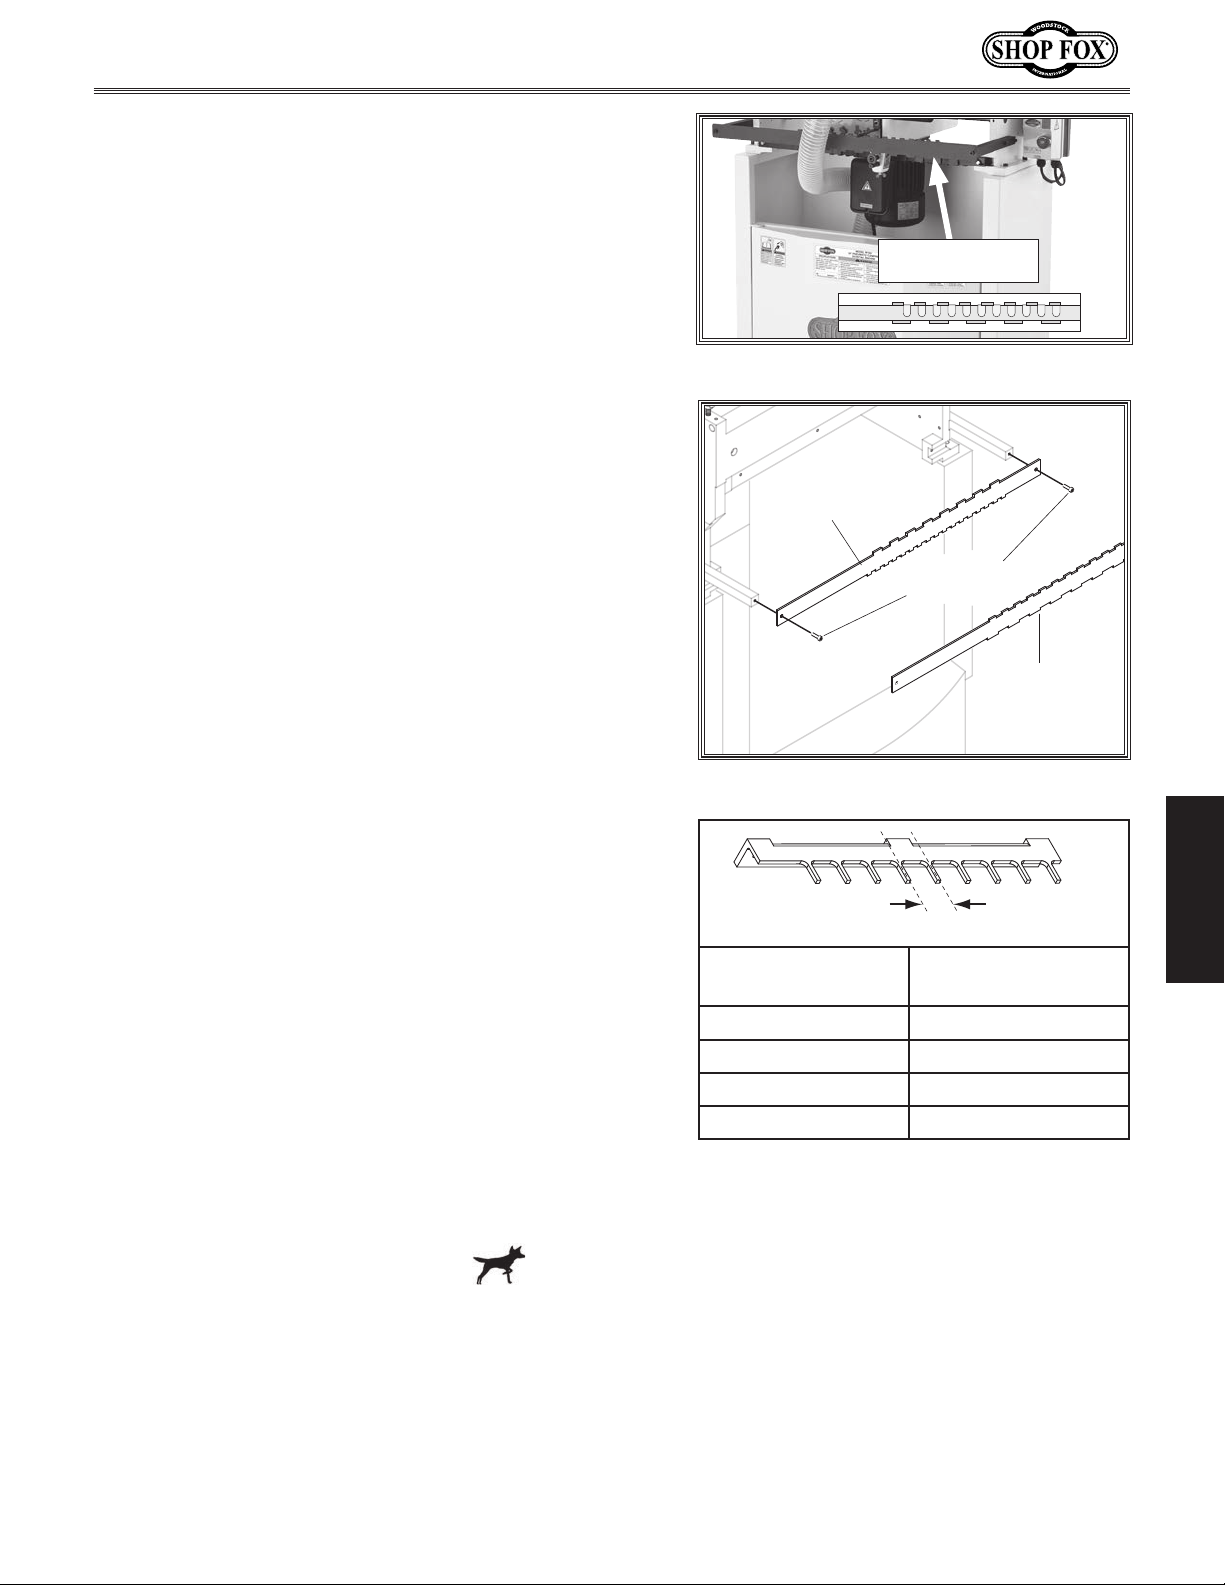
Use an adjustable wrench to loosen the hex nuts
2.
shown in Figure 18 away from the clamp mounting
bracket.
Step 2.
Vertical Clamp
Hex Nuts
Continued on next page
Horizontal Clamp
Hex Nuts
Figure 18. Hex nuts for adjusting clamping
thicknesses (only one side shown).
-20-
Page 23
Model W1805 (For Machines Mfd. Since 7/15)
3. Slide the clamp mounting bracket so the clamps
provide enough room to move workpieces in and out.
Note: Use a ruler to make sure that both sides are
adjusted equally; otherwise, contact area of the
clamp faces will not be uniform, which could result
in the workpieces slipping during operation.
4. Tighten the hex nuts against the clamp brackets to
hold them in place.
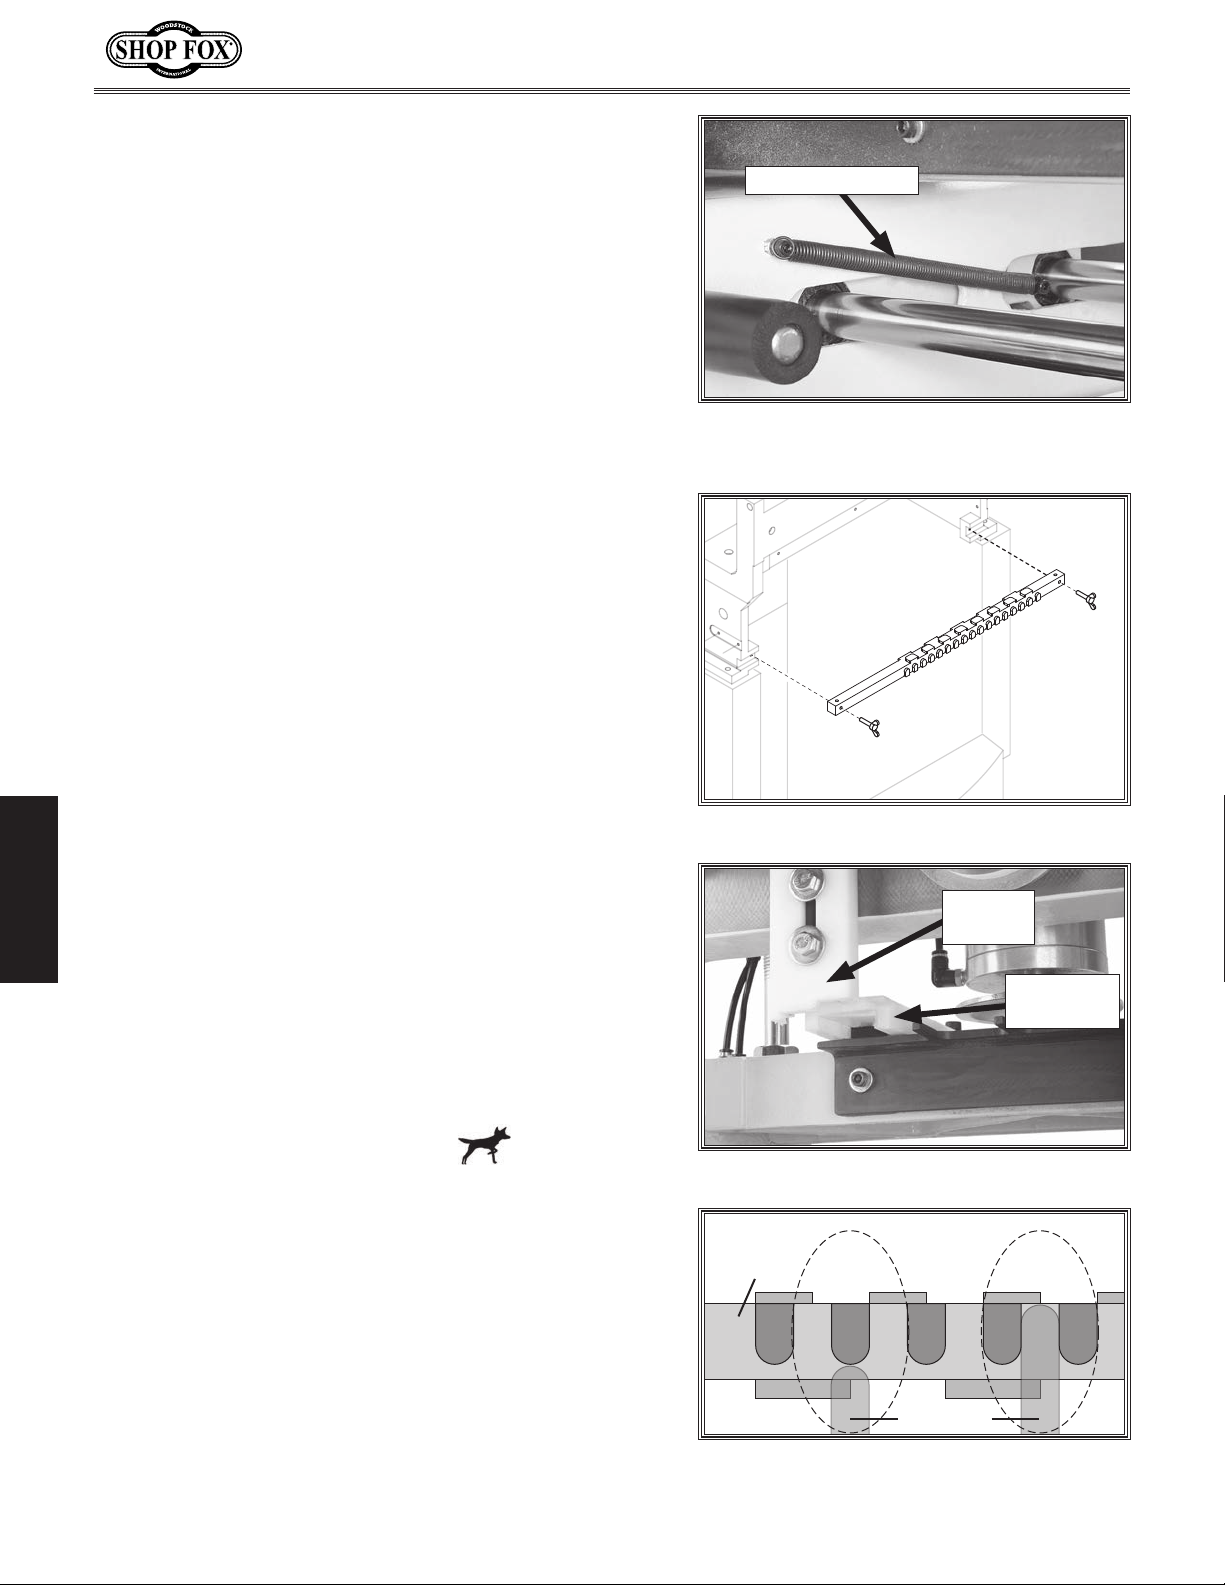
Changing Template Sizes
The template bar (Figure 19) has a different size dovetail
template on each of the four sides. The size of each
template is stamped into that side. The active template
size is always the side that is facing down. A tracer pin
connected to the headstock guides the cutter along the
template profile when cutting.
The template works in tandem with the indicator plate
and the fixed chaser.
Indicator Plate: Since the template bar is underneath the
cutting area and away from immediate operator view, the
top edge of the indicator plate mirrors the position of the
tracer pin along the template bar to help the operator
when cutting.
Template Bar
Figure 19. Template bar.
1" and 2"
Indicator Plate
Mounting
Cap Screws
1
1
⁄2" and 21⁄2"
Indicator Plate
Figure 20. Indicator plate installation.
OPERATIONS
Each indicator plate has two patterns. When mounted, the
top edge of the indicator plate must match the current
side of the template bar that is being used. Whenever
changing the template bar size, the indicator plate must
also be changed. Use the two mounting cap screws to
remove and change the indicator plate (see
Figure 20).
Fixed Chaser: The fixed chaser supports the vertical
workpiece, yet allows the cutter to cut the bottom of the
vertical workpiece without hitting the metal fixed chaser.
To prevent the cutter from contacting the fixed chaser,
use the fixed chaser that corresponds to the template size
shown in
Figure 21.
Continued on next page
Measuring Fixed Chaser Size
Template Bar Size Use Fixed Chaser
Size
1" 2"
1
1
⁄2" 3"
2" 2"
1
2
⁄2" 21⁄2"
Figure 21. Determining correct fixed
chaser.
-21-
Page 24
To change dovetail template size, do these steps:
Model W1805 (For Machines Mfd. Since 7/15)
1. Remove the extension spring shown in Figure 22,
and pull the headstock backward (toward you) to
clear the tracer pin of the template.
Remove the wing screw on each side of the template
2.
bar.
Slide the template bar out of the casting and
3.
reinstall it, as shown in Figure 23, so the desired
template size is facing down.
Lock the template in place with the wing screws,
4.
then replace the extension spring.
Setting Fences
The dovetail machine features HDPE (high density
polyethylene) plastic fences for both the horizontal and
vertical workpieces (see
into during operation to reduce tear-out.
The fences should be set so that the dovetails are evenly
distributed across the width of the workpiece. Setting the
fences requires attention to the "in" and "out" positions
of the tracer pin (see
in the "in" position, the cutter is cutting the workpiece.
When the tracer is in the "out" position, the cutter is
outside of the workpiece.
To set the fences, do these steps:
OPERATIONS
1. DISCONNECT MACHINE FROM POWER!
2. Remove the guard.
Figure 24). These fences are cut
Figure 25). When the tracer pin is
Extension Spring
Figure 22. Extension spring (located on
the right side of the headstock).
Template Bar
Wing
Screw
Wing
Screw
Figure 23. Template bar installation.
Vertical
Fence
Horizontal
Fence
3. Place the vertical workpiece on the support bar.
Continued on next page
-22-
Figure 24. HDPE fences.
Template
Bar
Out
Position
In
Position
Tracer Pin
Figure 25. Tracer pin positions (as viewed
from underneath template bar).
Page 25
Model W1805 (For Machines Mfd. Since 7/15)
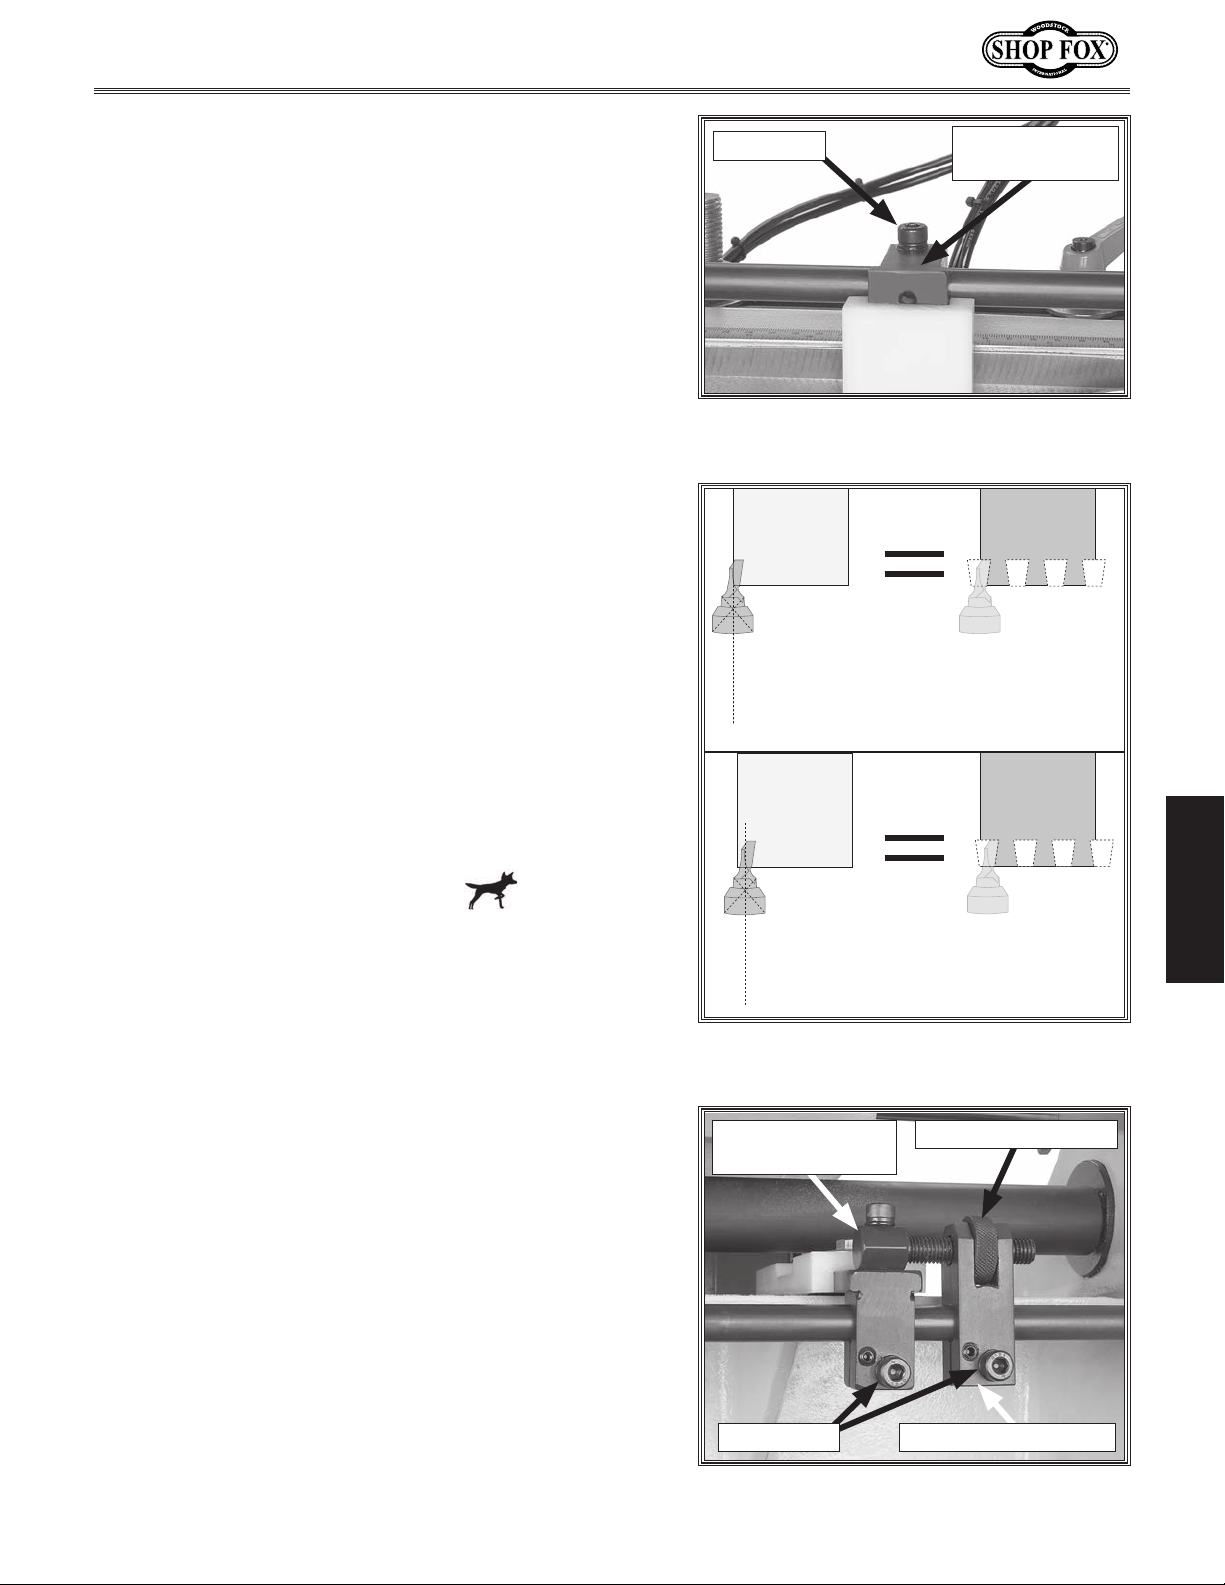
4. Loosen the cap screw on the vertical fence bracket
shown in Figure 26.
Align the left-hand edge of the vertical workpiece
5.
with the centerline of the cutter when the tracer
pin is in the "in" or cutting position. This position
will make the first cut in the vertical workpiece half
the width of the cutter.
Figure 27 illustrates this
concept.
Note: If your workpiece width is not evenly divisible
by the template size, then setting the fences for
even cut distribution is a matter of judging the best
possible position by eye.
Remember the position of the left-hand edge of the
6.
vertical workpiece on the vertical fence scale, and
move the vertical workpiece out of the way.
Align the right-hand edge of the vertical fence with
7.
the same position on the scale from the previous
step, then lock the vertical fence in place with the
cap screw.
Cap Screw
Vertical Fence
Bracket
Figure 26. Vertical fence adjustment cap
screw.
Vertical
Workpiece
Cutter Centerline
Aligned
Vertical
Workpiece
Even Cut
Distribution
with Edge
Familiarize yourself with the horizontal fence
8.
adjustment components in Figure 28.
Loosen both cap screws shown in Figure 28.
9.
Continued on next page
Vertical
Workpiece
Cutter Centerline
NOT Aligned
Vertical
Workpiece
Uneven Cut
Distribution
with Edge
Figure 27. Aligning cutter start location
with the vertical workpiece.
Main Adjustment
Micro-Adjust Wheel
Bracket
OPERATIONS
-23-
Micro-Adjust BracketCap Screws
Figure 28. Horizontal fence adjustment
components.
Page 26
Model W1805 (For Machines Mfd. Since 7/15)
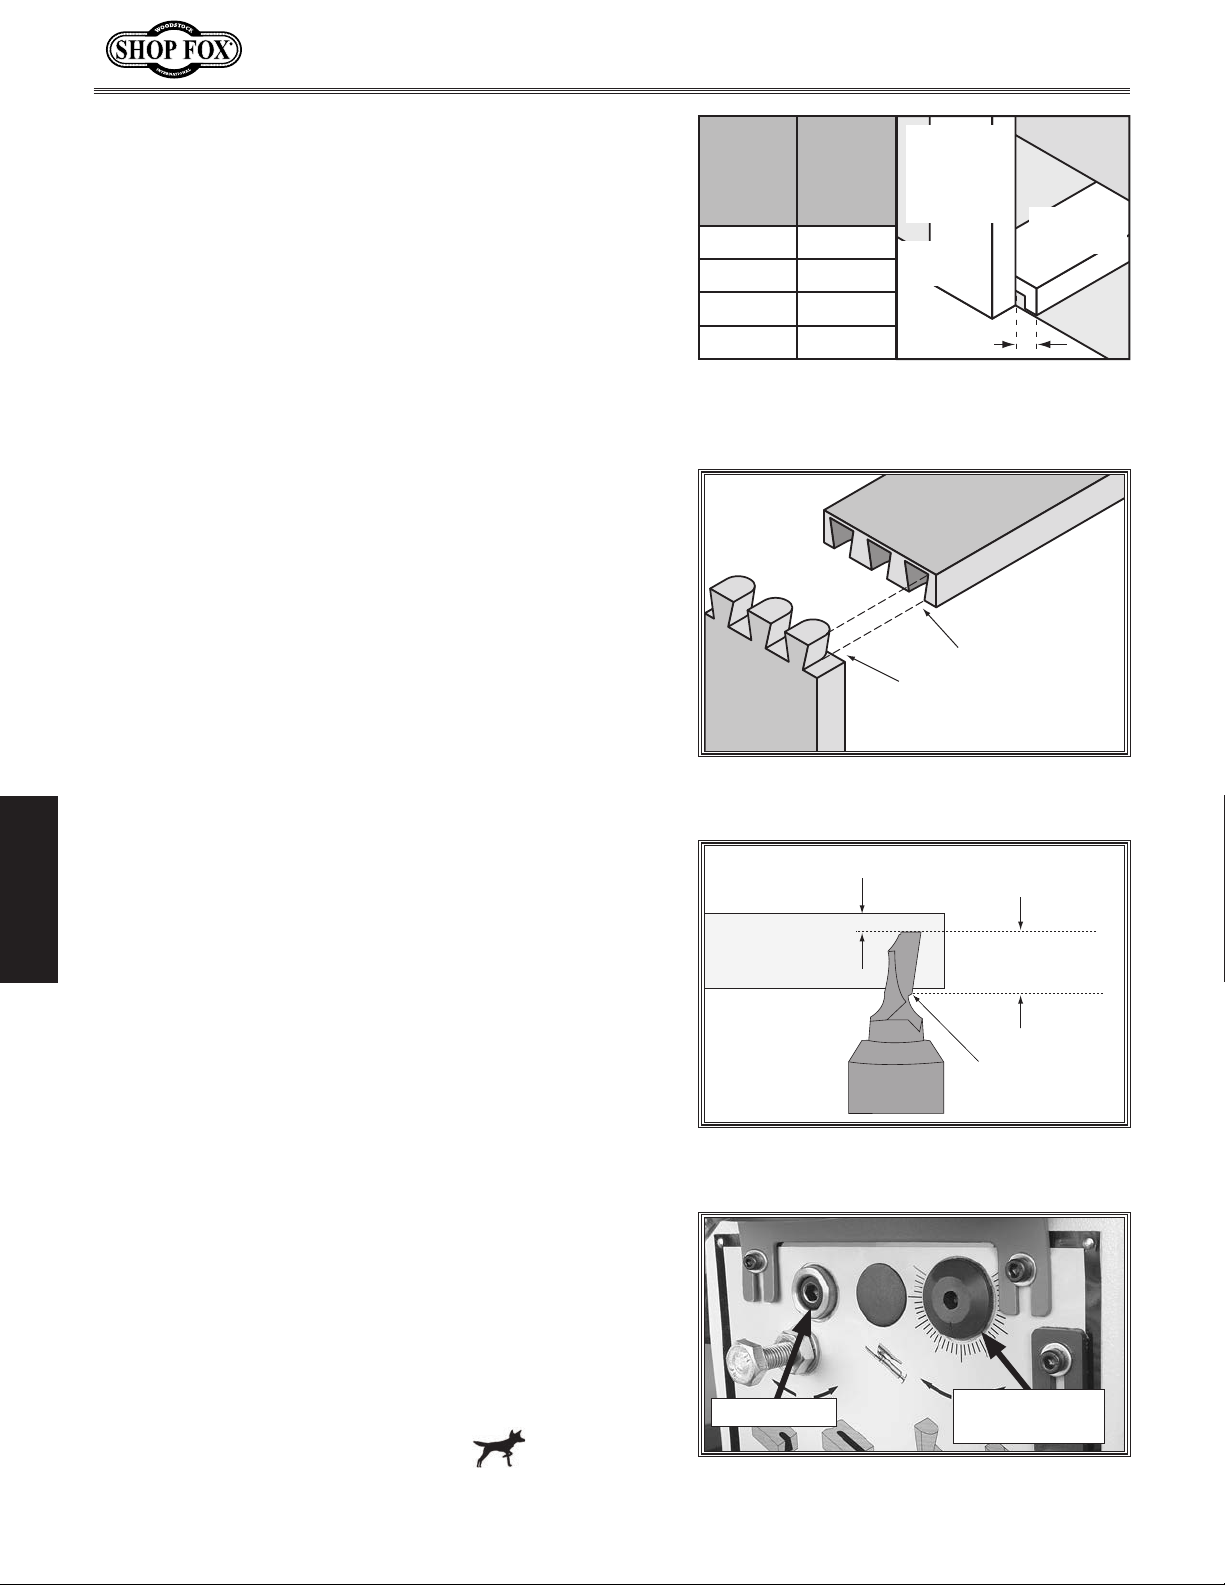
Offset
1
⁄2"
Horizontal
Fence
Vertical
Fence
Offset
Example
for 1"
Template
10. Using the scale on each table as a guide, adjust the
right-hand edge of the horizontal fence so it is offset
half the amount of the template size being used.
For example, if the template size is 1", offset the
right-hand edge of the horizontal fence 1⁄2" from the
right-hand edge of the vertical fence, as shown in
Figure 29.
Lock the cap screw on the micro-adjust bracket,
11.
and use the micro-adjust wheel to set the horizontal
fence in the exact position.
Tighten the cap screw on the main adjustment
12.
bracket to lock the horizontal fence.
Cutter Height
The cutter height dictates the tail height on the vertical
workpiece and the socket height on the horizontal
workpiece (see
The cutter height range is restricted by the size of the
cutter (see
edge should never be set above the bottom of the
workpiece.
A taller cutter height is stronger due to larger tails and
pins, so maximizing the cutter height is preferred in most
situations.
Figure 30).
Figure 31). The lowest point of the cutting
Horz.
Template
Size
1"
1
1
⁄2"
2"
1
2
⁄2" 11⁄4"
Fence
Offset
Distance
1
⁄2"
3
⁄4"
1"
Figure 29. Fence offset sizes for each
template size and example offset diagram
for 1" template.
Socket Height
Tail Height
Figure 30. Example of cutter and socket
height.
1
⁄8" Minimum (recommended)
OPERATIONS
To set the cutter height, do these steps:
DISCONNECT MACHINE FROM POWER!
1.
Place the horizontal workpiece on the horizontal
2.
table against the fence, and clamp the workpiece
down.
Remove one end of the headstock spring, and move
3.
the cutter in front of the horizontal workpiece.
Use a 6mm hex wrench to loosen the cutterhead lock
4.
shown in Figure 32.
Use a 6mm hex wrench to adjust the cutter up or
5.
down. Leave at least 1⁄8" of material between the
bottom of the board and the bottom of the cutter.
Tighten the cutterhead lock.
6.
Continued on next page
Horizontal
Workpiece
(end view)
Cutter
Cutter Height
Range
Lowest Point
of Cutter
Figure 31. Understanding the cutter
height range compared to the workpiece.
Cutter Lock
Cutter Height
Adjustment
Figure 32. Cutter lock and adjustment
height.
-24-
Page 27
Model W1805 (For Machines Mfd. Since 7/15)
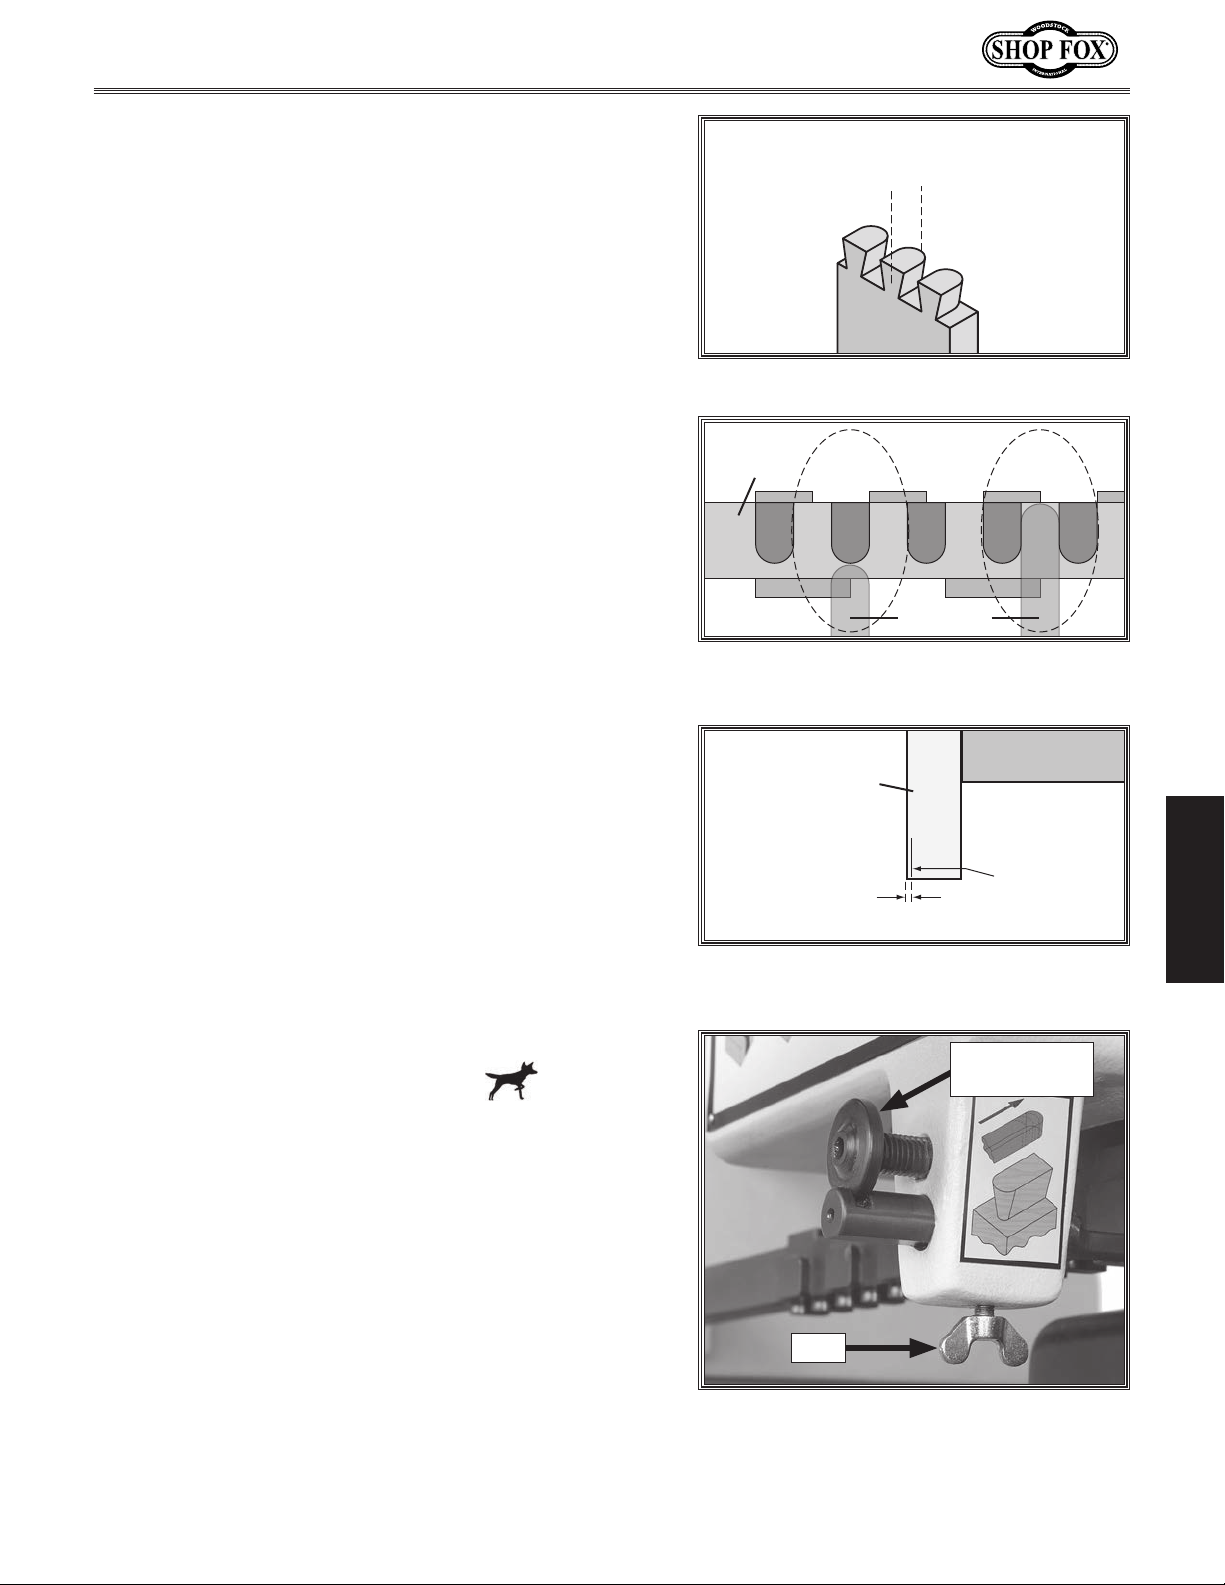
Tail Thickness
Figure 33 shows the tail thickness.
The tail thickness is controlled by adjusting the tracer pin
when it is in the "out" position on the template bar, as
shown in
To set the tail thickness, do these steps:
DISCONNECT MACHINE FROM POWER!
1.
2. Draw a small pencil line on the edge of the vertical
Install the vertical workpiece so the side of the
3.
Figure 34.
workpiece approximately 1⁄16" from the side of the
workpiece (see
Figure 35).
board closest to the pencil line is facing out, as
shown in
Figure 35, and clamp the workpiece into
position against the vertical fence.
Tail Thickness
Figure 33. Example of tail thickness.
Template
Bar
Out
Position
In
Position
Tracer Pin
Connect the spring to the headstock.
4.
5. Move the headstock just to the right of the
workpiece, and put the tracer pin in the "out"
position on the template.
Stand to the right-hand side of the machine, and
6.
look across the table at the cutter relationship to
the vertical workpiece. This viewing position will
help you align the cutter with the workpiece during
the next step.
Note: Familiarize yourself with the tracer pin
controls shown in Figure 36 if this is the first time
you have adjusted it.
Continued on next page
Figure 34. Tracer pin positions on
template.
Vertical
Workpiece
Table
(Side View)
Pencil
1
⁄16"
Figure 35. Pencil line location on vertical
workpiece.
Line
Adjustment
Thumbwheel
OPERATIONS
-25-
Lock
Figure 36. Tracer pin controls.
Page 28
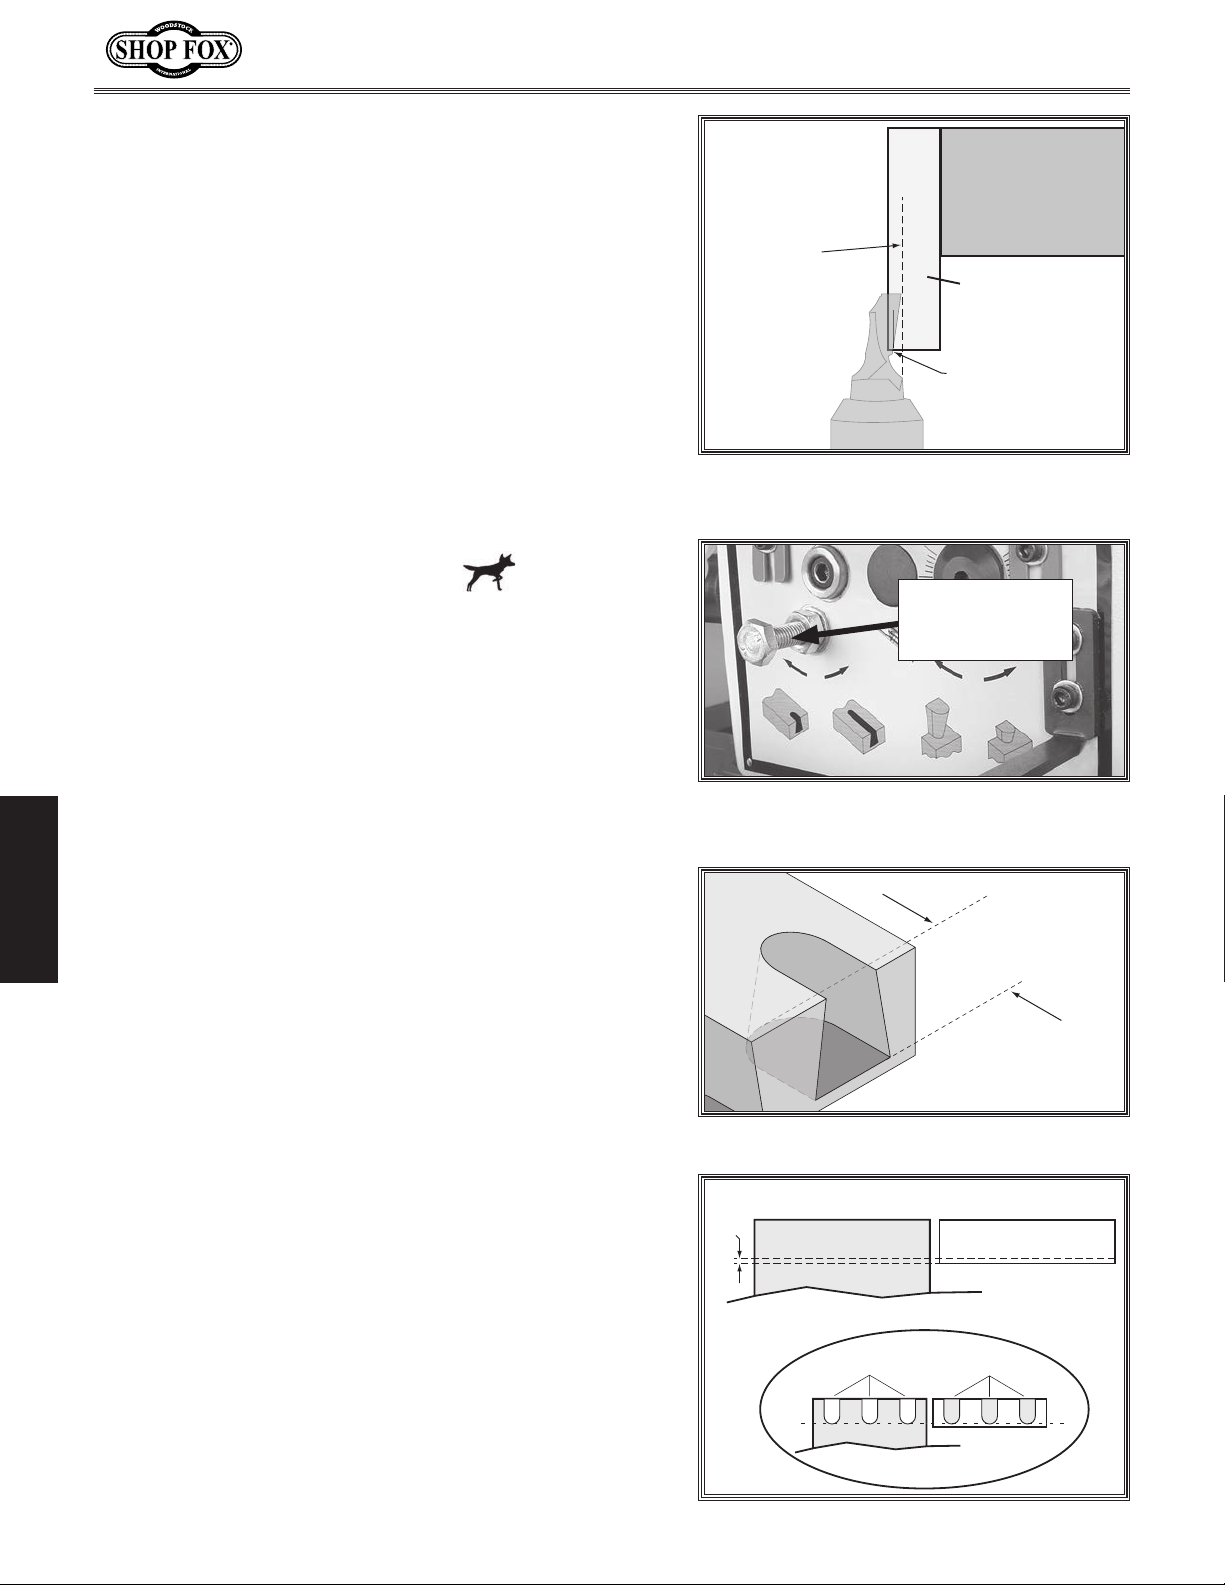
7. Unlock the tracer pin, and adjust the thumbwheel as
necessary until the cutter is positioned as shown in
Figure 37.
Model W1805 (For Machines Mfd. Since 7/15)
(Side View)
Lock the tracer pin.
8.
Cutter Depth Stop
The cutter depth stop adjustment bolt (Figure 38)
dictates the depth of the sockets (
controlling how far the cutter will cut into the horizontal
workpiece.
The cutter depth should be the same as the tail thickness,
so that when the joint is assembled the tails are flush
with the pins (
Figure 40).
Continued on next page
Figure 39) by
Cutting edge
rotated to
maximum
point of rotation
from side view.
Table
Vertical
Workpiece
Cutter aligned
with pencil line
at the bottom of
Cutter
the workpiece.
Figure 37. Cutter position for setting tail
thickness (as viewed from the side).
Cutter Depth
Stop Adjustment
Bolt
OPERATIONS
Figure 38. Cutter depth stop adjustment
bolt.
Socket Depth
Figure 39. Socket depth.
Horizontal Workpiece Vertical Workpiece
1
⁄16"
Board Face Board End
...as cut
Sockets
Tails
-26-
Figure 40. Understanding correct cutter
depth.
Page 29
Model W1805 (For Machines Mfd. Since 7/15)
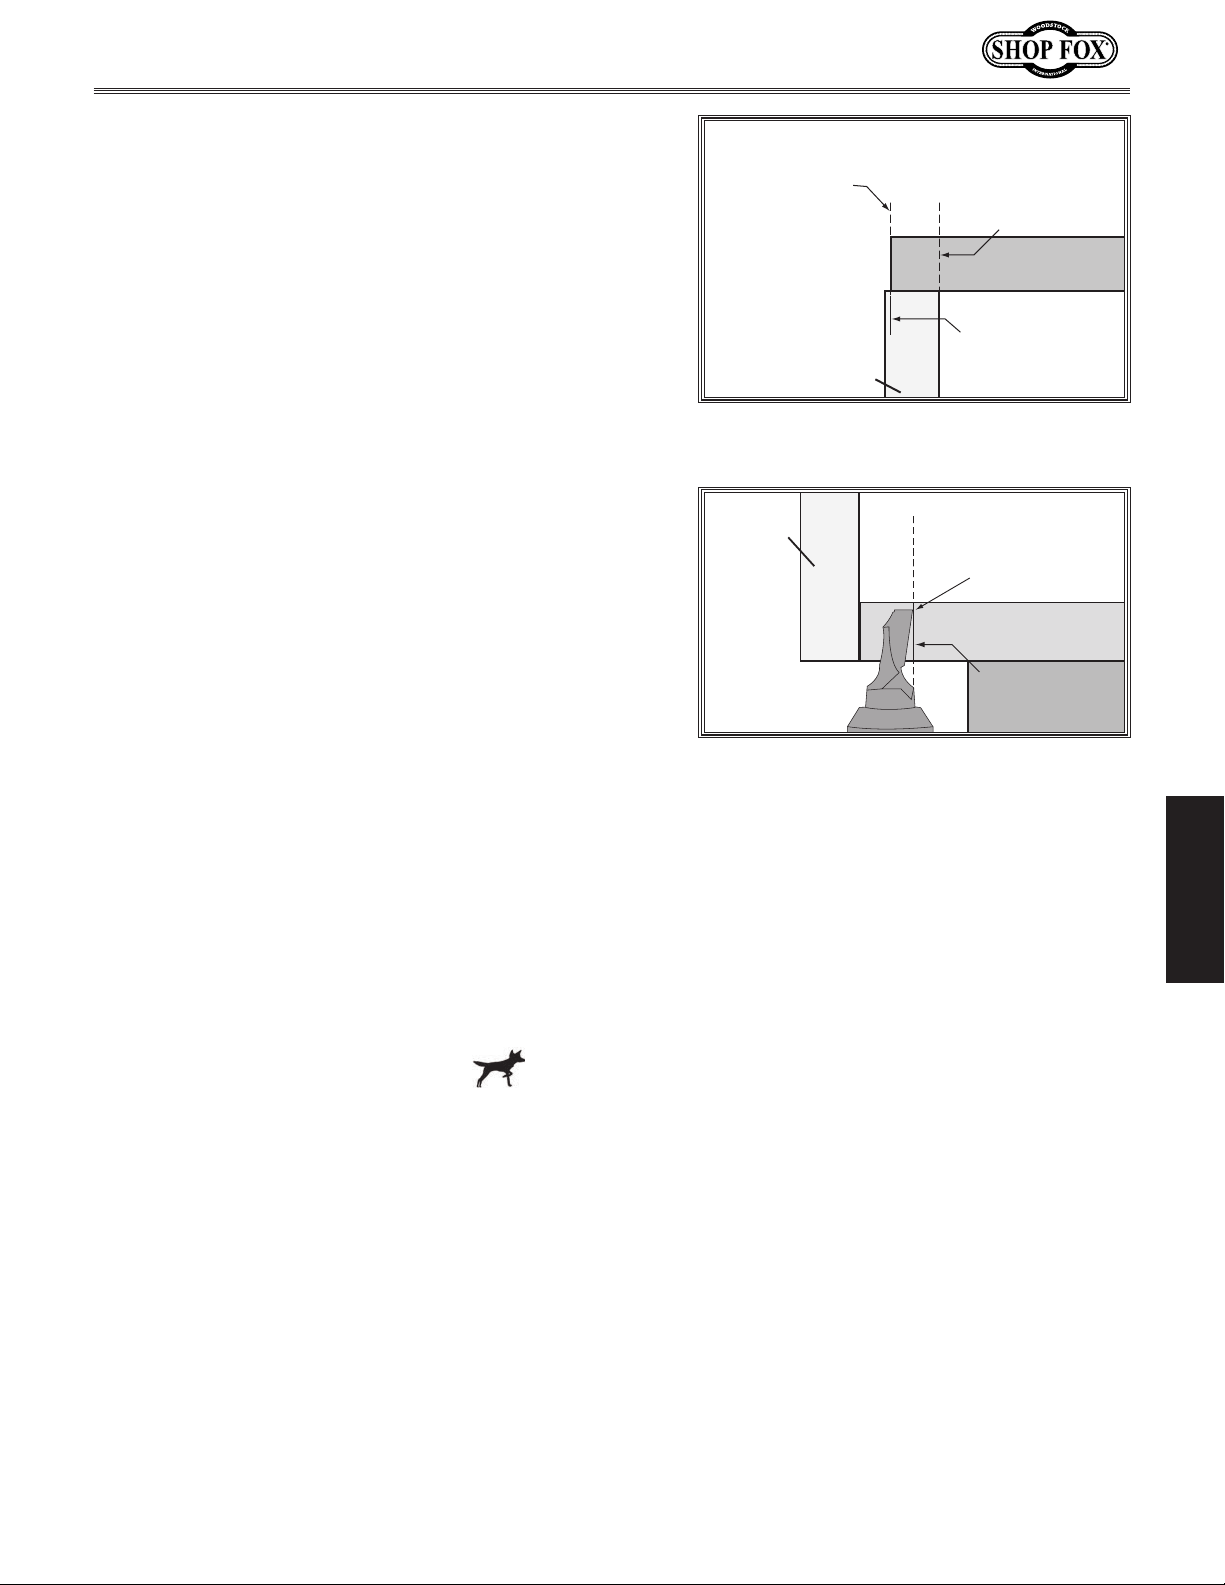
To set the cutter depth stop, do these steps:
1. DISCONNECT MACHINE FROM POWER!
2. On a workbench, copy the "Tail Thickness" dimension
from the vertical workpiece to the horizontal
workpiece (
Clamp the vertical workpiece in position on the
3.
Figure 41).
machine, then clamp the horizontal workpiece in
place against the vertical workpiece.
Move the cutter to the right of the horizontal
4.
workpiece and make sure the tracer pin is in the "in"
position.
Rotate the cutter until the leading edge is at the
5.
farthest point in rotation toward the rear of the
machine.
From the right-hand side of the machine, look across
6.
the table at the cutter position in relation to the
pencil line.
Adjust the cutter depth bolt until the tip of the
7.
cutter aligns with the pencil line (Figure 42), then
tighten the hex nut.
Edge of
Horizontal
Piece Aligned
w/Pencil Line
Cutter Depth
Pencil Line
Here
Horizontal
Workpiece
(Side View)
Make
Vertical
Workpiece
Figure 41. Marking horizontal workpiece
to set the cutter depth.
Vertical
Workpiece
(Side View)
Cutter
Figure 42. Cutter position to set cutter
depth stop (viewed from the side).
Tail Thickness
Pencil Line
Cutter tip at
farthest point
of rotation from
the side view.
Horizontal
Workpiece
Pencil Line
Table
OPERATIONS
Testing Machine Setup
Testing the setup requires you to make cuts and adjust
the cutter until the dovetail fit is perfect. Be aware that
the drawer you make during this procedure may end up as
scrap. To achieve good dovetails, you must have prepared
your stock as described in
Continued on next page
Stock Preparation on Page 18.
-27-
Page 30
Model W1805 (For Machines Mfd. Since 7/15)
RIGHT
or
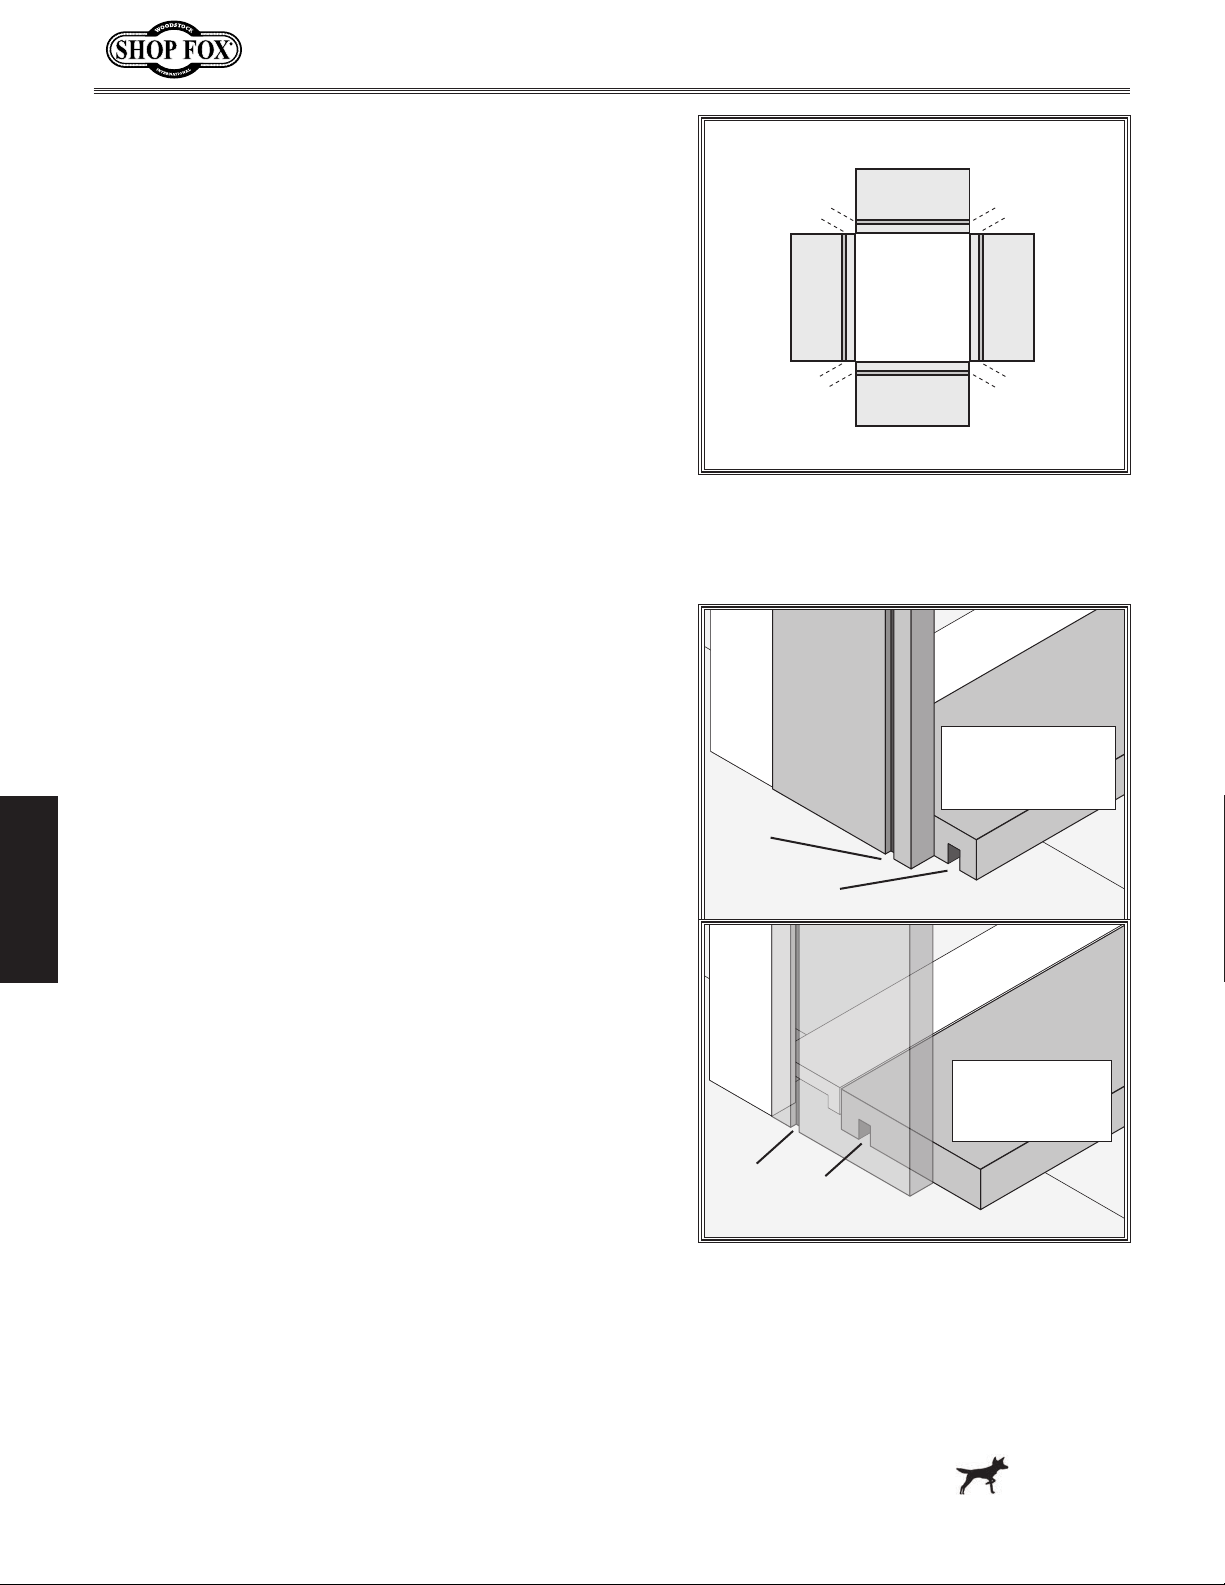
The standard cutting order is shown in
Figure 43. Figure
44 shows the workpieces positioned with the dadoes close
to or away from the fences.
To make a test cut, do these steps:
1. Position the RIGHT workpiece on the vertical support
bar, as shown in the top illustration in
Figure 44
(with the dado positioned out and opposite the
fence), then clamp down the RIGHT workpiece.
Place the BACK workpiece on the horizontal table,
2.
as shown in the top illustration in Figure 44 (with
the dado positioned down and opposite the fence),
then clamp down the BACK workpiece. The bottom
of both workpieces should be flush with each other
and both workpieces should be firmly against their
respective fences.
Position the cutter so it is not touching the fences or
3.
workpieces.
INSTALL AND SECURE THE GUARD!
4.
5. Connect the machine to the power source.
6. Make the test cut as described below, but read all of
the steps before starting, so you do not have to stop
after you begin cutting:
Start the cut on the left-hand side of the vertical
a.
piece (half of the cutter will cut into the plastic
OPERATIONS
fences), then carefully follow the template
from left-to-right, making sure the tracer pin
maintains contact with the template (otherwise
unnecessary tear-out will occur).
After clearing the workpieces, do a cleanup pass
b.
by bringing the headstock back the opposite
direction and following the template from rightto-left.
c. Turn the machine OFF, and position the cutter
clear of the workpieces and fences.
Remove the workpieces from the machine and test
7.
fit the dovetail joint.
Cut 4:
Position
Dadoes Close
to Fence
LEFT RIGHT
Cut 3:
Position
Dadoes Away
from Fence
BACK
FRONT
Cut 1:
Position
Dadoes Away
from Fence
Cut 2:
Position
Dadoes Close
to Fence
Figure 43. Drawer pieces laid out and
marked inside face up; cutting order and
workpiece position against fences also
shown.
LEFT
Vertical
Fence
RIGHT
or
LEFT
Horizontal
Fence
FRONT
or
BACK
FRONT
Cuts 1 & 3
or
BACK
Dadoes Away
from Fences
Dado
Out
Dado
Down
Horizontal
Fence
FRONT
or
BACK
Vertical
Fence
RIGHT
or
LEFT
Cuts 2 & 4
Dadoes Close
to Fences
Dado
Out
Dado
Down
Figure 44. Workpiece positions for cuts.
Carefully examine how the tails fit into the sockets.
8.
The tails should fit into the sockets tightly and
both workpieces should be flush with each other.
Typically, fine-tuning the dovetail joint fit requires
balancing socket depth and the cutter adjustment,
as follows:
-28-
Continued on next page
Page 31
Model W1805 (For Machines Mfd. Since 7/15)
— If the workpieces do not fit together or if the fit is
too tight, then adjust the cutter to take a larger
cut and repeat "Cut 1."
— If the workpieces fit together too loosely, adjust
the cutter to take a smaller cut and do "Cut 2."
— If the tails fit easily side-to-side into the sockets,
but do not go down far enough, adjust the socket
depth deeper.
— If the tails fit easily side-to-side into the sockets,
but go too far down, adjust the socket depth
shallower.
Adjusting Cutter
The cutter rotates eccentrically in the spindle, which
allows it to be adjusted for control of the dovetail joint
"fit" when assembled.
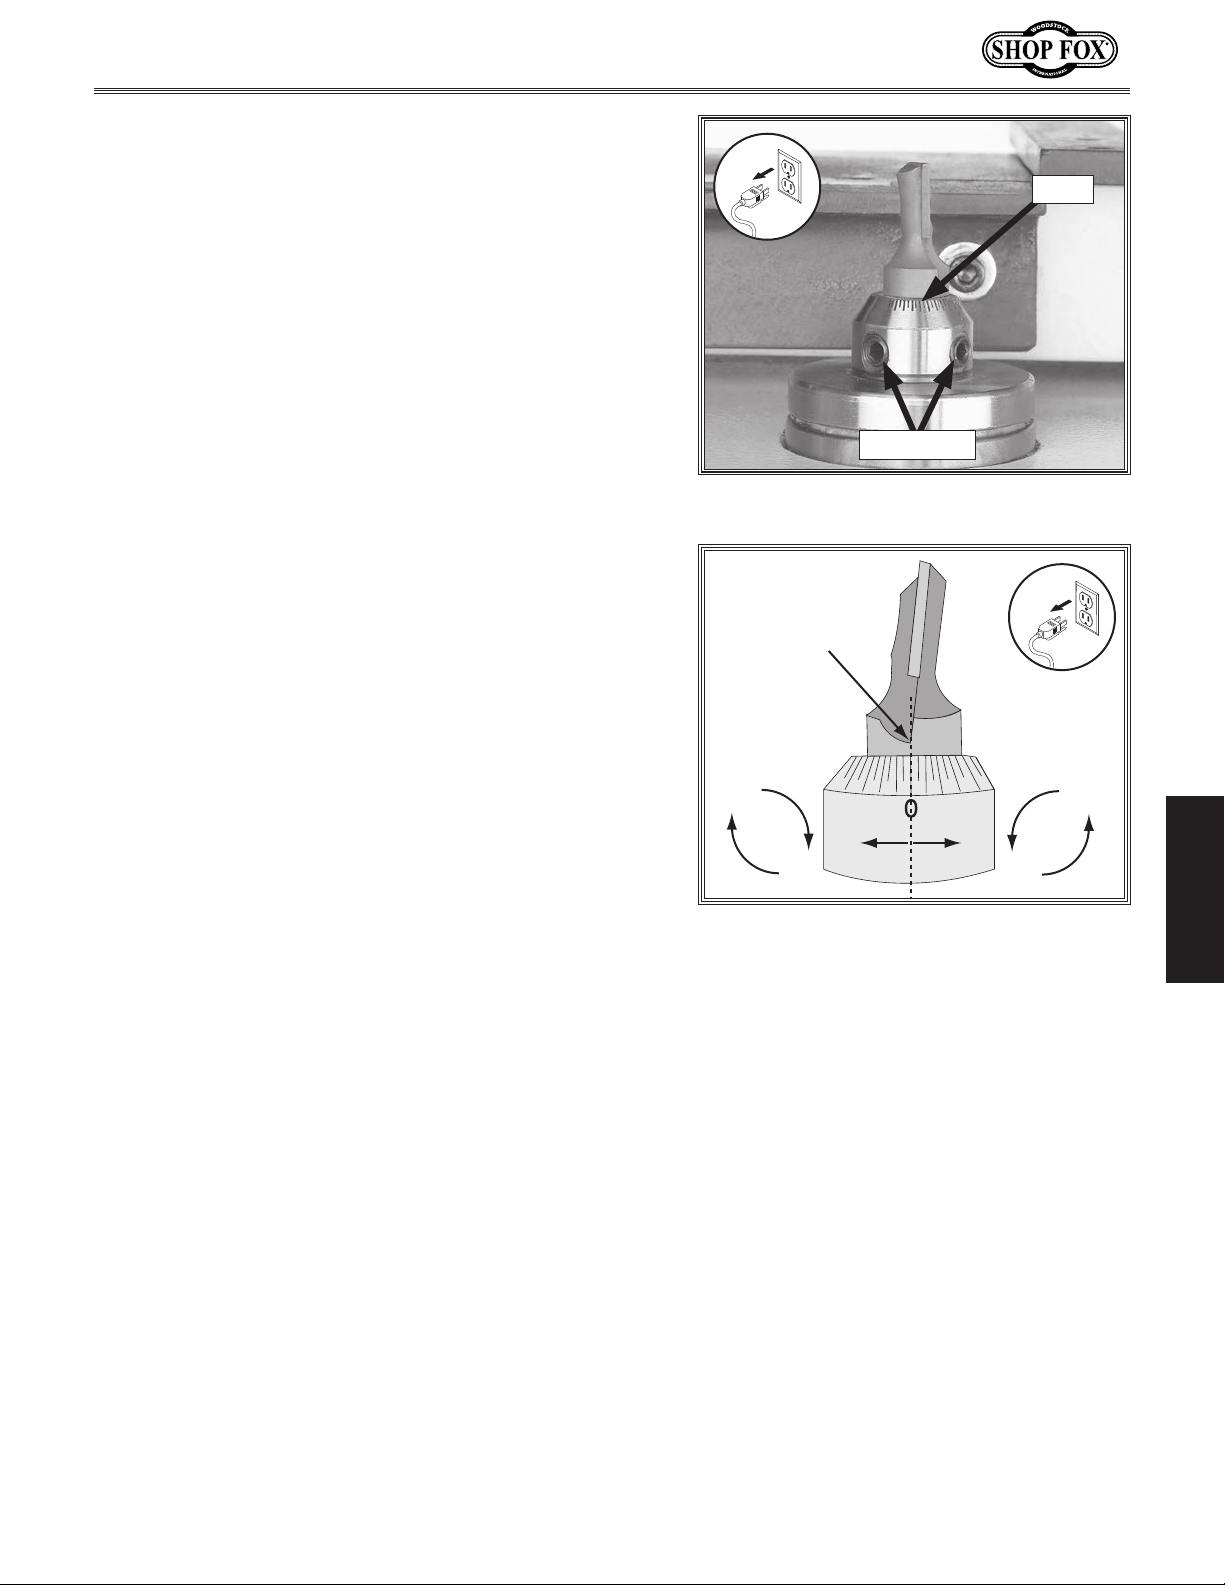
Two set screws hold the cutter in position and a spindle
scale is provided for monitoring the cutter position during
adjustments (
To adjust the cutter, do these steps:
Figure 45).
Scale
Set Screws
Figure 45. Cutter adjustment controls.
Lowest
Point
of Cutter
Groove
(-)
Take a
smaller cut
(+)
Take a
larger cut
DISCONNECT MACHINE FROM POWER!
1.
2. Remove the guard.
3. Use a 4mm hex wrench to loosen the two set screws
on the spindle just enough to rotate the cutterhead.
(Loosening the two set screws too much may cause
the cutter to drop down in the spindle and throw off
other adjustments.)
Rotate the cutter inside the spindle as necessary to
4.
take a smaller or larger cut (see Figure 46). Use the
highest point in the cutter groove to keep track of
the cutter position during adjustments.
Tighten the two set screws to secure the cutter in
5.
place.
Make sure the spring is connected to the headstock.
6.
7. Install the guard.
(-)
Figure 46. Understanding cutter
adjustments.
(+)
OPERATIONS
8. Test the new cutter setting by making a cut.
9. Repeat cutter adjustment as necessary until the fit
is satisfactory. ALWAYS DISCONNECT POWER BEFORE
ADJUSTING CUTTER!
-29-
Page 32
MAINTENANCE
Schedule
Daily Maintenance (8 Hours)
• Check/tighten cutter set screws.
• Clean debris/sawdust from clamps to ensure that
they do not interfere with the clamping ability.
• Clean/vacuum dust buildup off motor.
• Clean and lubricate unpainted cast iron portions of
the table and the headstock travel rods with a light
oil.
• Check/replace damaged power cords or wires.
• Check/add air tool oil to the air supply unit
lubricator.
Model W1805 (For Machines Mfd. Since 7/15)
MAKE SURE that your machine is
unplugged during all maintenance procedures! If this warning is ignored, serious personal injury may occur.
• Check/drain the air supply unit water filter. (Drain
by sliding the white shaft to the other side.)
Weekly Maintenance (40 Hours)
• Grease spindle with multi-purpose lithium grease.
Monthly Maintenance (320 Hours)
• Belt tension, damage, or wear.
Cleaning
Vacuum excess wood chips and sawdust, and wipe off the
remaining dust with a dry cloth. If any resin has built up,
use a resin dissolving cleaner to remove it.
Protect the unpainted cast iron surfaces on the table
MAINTENANCE
by wiping the table clean after every use—this ensures
that moisture from wood dust does not remain on bare
metal surfaces. Tables can be kept rust-free with regular
applications of a quality metal protectant/lubricant.
Lubrication
The bearings in the machine are sealed and lubricated
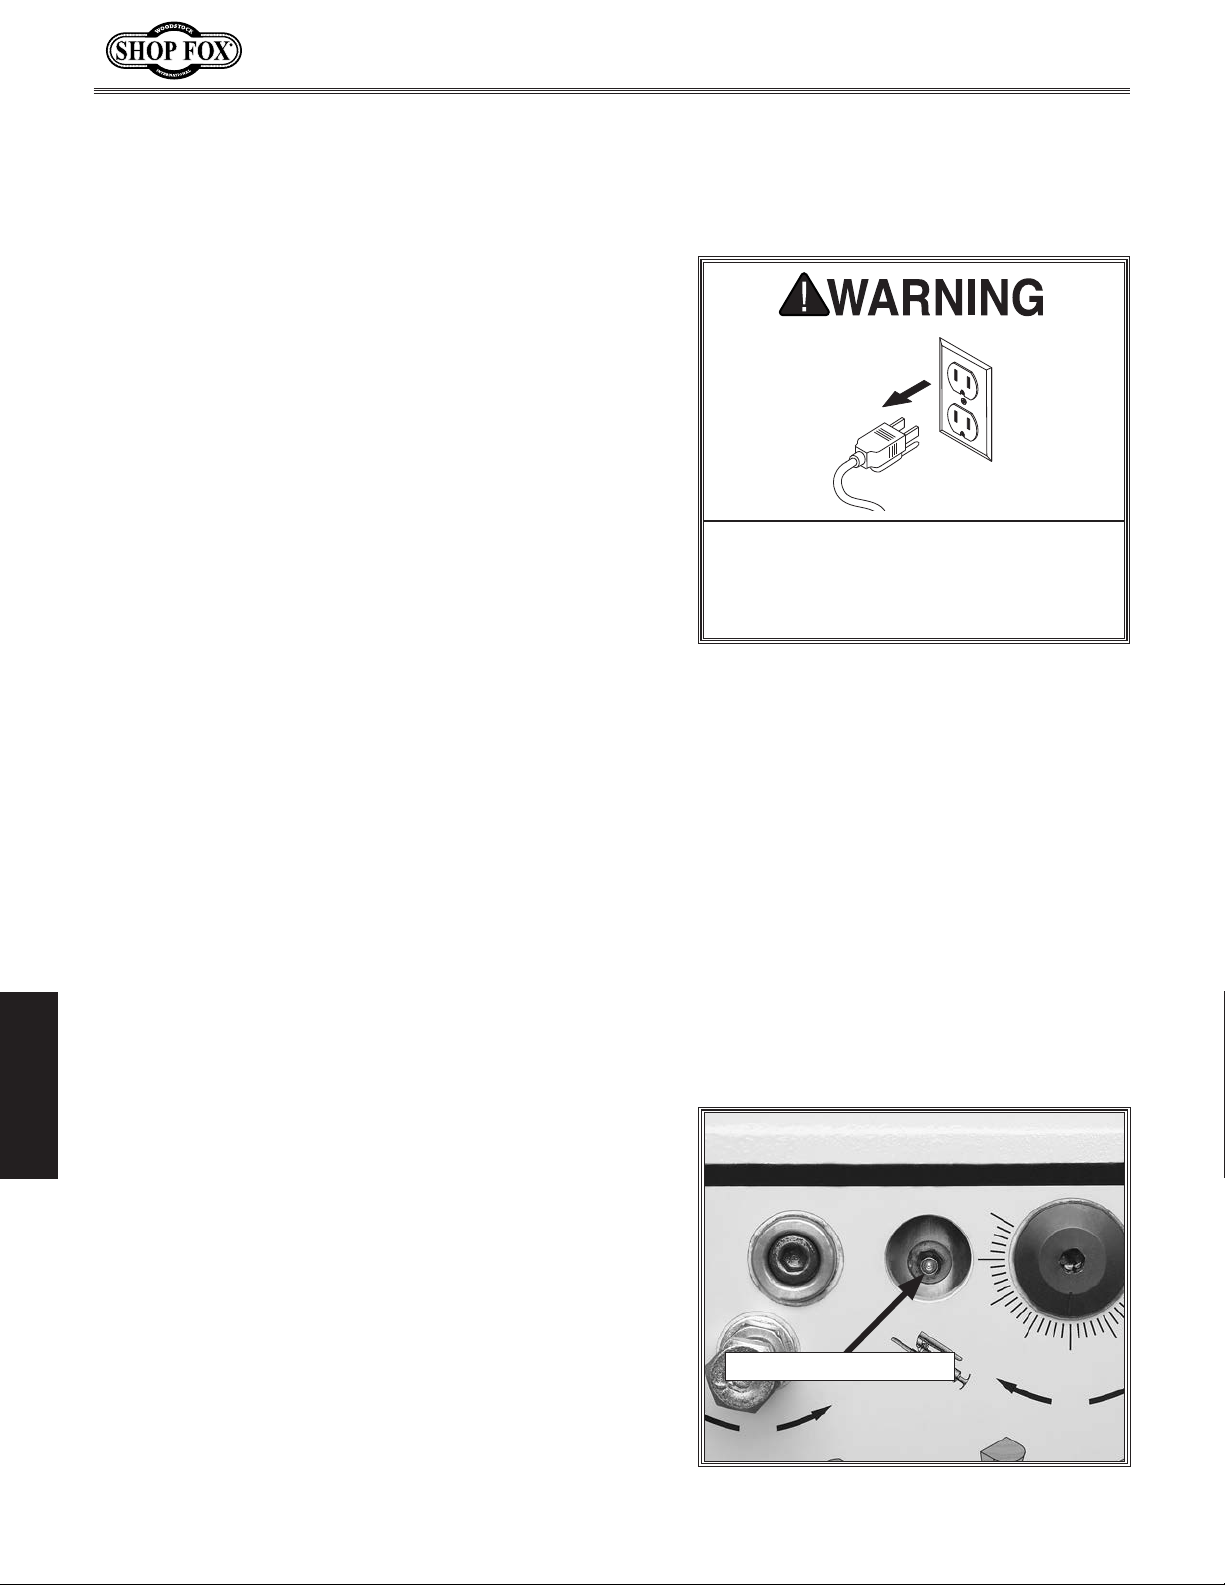
for life. The spindle has one grease fitting that must be
greased approximately every 40 hours or one week of
regular use (refer to
connect the fitting to a grease gun and give the spindle
one pump of multi-purpose lithium grease.
Figure 47). To grease the spindle,
-30-
Spindle Grease Fitting
Figure 47. Spindle grease fitting.
Page 33
Model W1805 (For Machines Mfd. Since 7/15)
This section covers the most common service adjustments
or procedures that may need to be made during the life
of your machine.
If you require additional machine service not included
in this section, please contact Woodstock International
Technical Support at (360) 734-3482 or send e-mail to:
[email protected].
SERVICE
General
Cutter Replacement
When the cutter gets dull, or if it gets damaged, it
must be replaced. Dull cutters can be resharpened by
a professional, but cutters are inexpensive and easily
replaced.
Tools Needed Qty
Hex Wrench 4mm ...............................................1
To replace the cutter, do these steps:
DISCONNECT MACHINE FROM POWER!
1.
Remove the guard.
2.
3. Loosen the two set screws that hold the cutter in
the spindle. (The set screws must be backed out
half-way before the cutter can be removed.)
Slide the cutter out and insert the new one.
4.
5. Tighten the two set screws to secure the cutter in
place.
MAKE SURE that your machine is
unplugged during all service procedures! If this warning is ignored, serious personal injury may occur.
6. Replace the guard.
Belt Tension
A flat belt transfers power from the motor to the cutter
spindle. This belt stretches with use and periodically
needs to be tensioned. If the cutter lacks power, stops
spinning, or cuts slower than normal, then the belt may
need to be tightened.
Continued on next page
SERVICE
-31-
Page 34
Tools Needed Qty
Hex Wrench 6mm ...............................................1
To tighten the belt, do these steps:
1. DISCONNECT MACHINE FROM POWER!
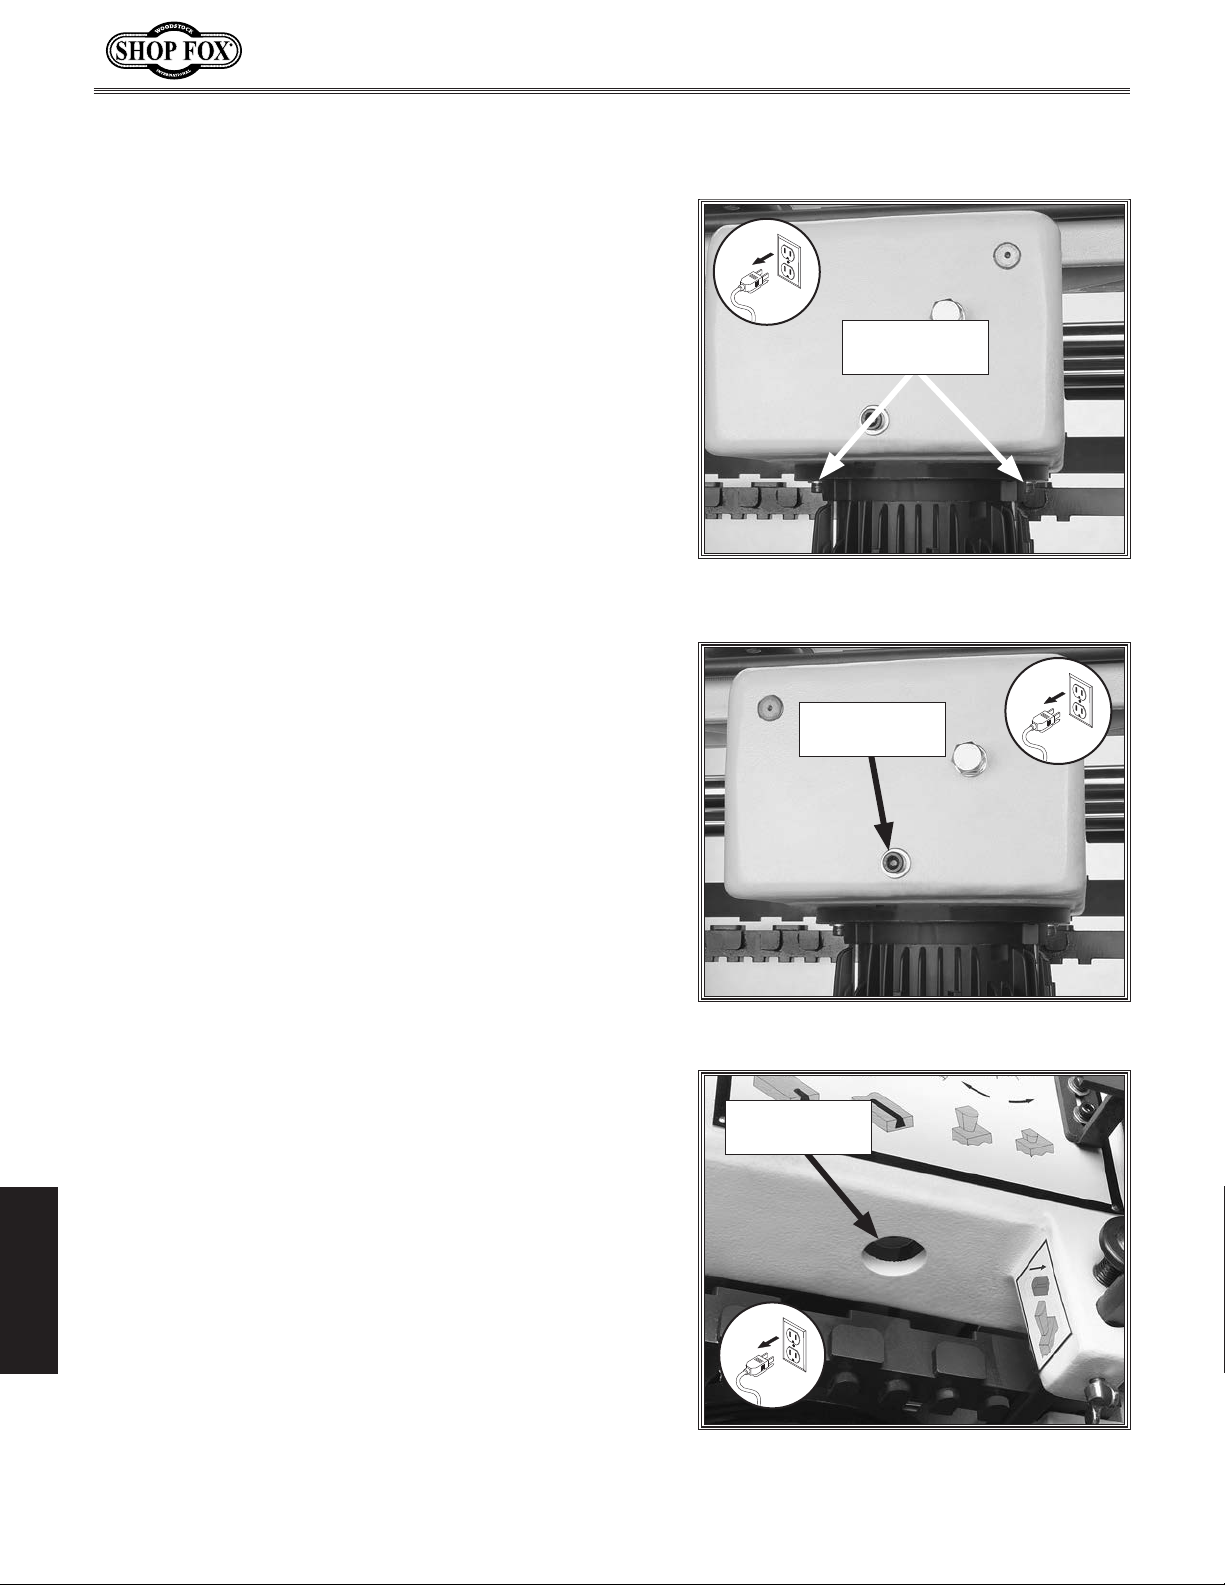
Loosen the two motor mount cap screws shown in
2.
Figure 48.
Turn the belt tension bolt, shown in Figure 49,
3.
clockwise to tension the belt.
Note: Each time you adjust the belt tension, only
turn the bolt one full turn. This will prevent overtightening the belt, which can lead to premature
bearing failure in the motor and spindle.
Belt Replacement
Model W1805 (For Machines Mfd. Since 7/15)
Motor Mount
Cap Screws
Figure 48. Motor mount cap screw
locations.
If the belt is left loose, it can stop during operation while
the pulley continues to spin. This scenario will burn the
belt, which will create a horrible vibration and smell of
burned rubber. If this ever happens, then the belt must
be replaced before continuing operations.
Tools Needed Qty
Hex Wrench 6mm ...............................................1
To replace the belt, do these steps:
1. DISCONNECT MACHINE FROM POWER!
Lower the cutter as far as it will go.
2.
3. Remove the dust plug shown in Figure 50 to access
the top of the belt.
Loosen the two motor mount cap screws shown in
4.
Figure 48.
Turn the motor tension bolt, shown in Figure 49,
5.
counterclockwise to loosen the belt.
Belt Tension
Bolt
Figure 49. Belt tension bolt.
Dust Plug
Access Hole
Slide the belt over the top of the spindle shaft and
6.
SERVICE
off of the motor pulley.
Reinstall and tension the new belt.
7.
8. Replace the dust plug, and tighten the motor mount
cap screws.
Figure 50. Dust plug removed to see top
of cutter spindle for belt removal.
-32-
Page 35
Model W1805 (For Machines Mfd. Since 7/15)
These pages are current at the time of printing. However, in the spirit of improvement, we may make
changes to the electrical systems of future machines. Compare the manufacture date of your machine to
If there are differences between your machine and what is shown in this section, call Technical Support
for assistance BEFORE making any changes to the wiring on your machine. An updated
machine before calling. This information can be found on the main machine label.
Electrical Safety Instructions
the one stated in this manual, and study this section carefully.
at (360) 734-3482
wiring diagram may be available. Note: Please gather the serial number and manufacture date of your
SHOCK HAZARD. Working on wiring that is
connected to a power source is extremely
dangerous. Touching electrified parts will
result in personal injury including but not
limited to severe burns, electrocution,
or death. Disconnect the power from
the machine before servicing electrical
components!
QUALIFIED ELECTRICIAN. Due to the inherent
hazards of electricity, only a qualified
electrician should perform wiring tasks on
this machine. If you are not a qualified
electrician, get help from one before
attempting any kind of wiring job.
WIRE CONNECTIONS. All connections must
be tight to prevent wires from loosening
during machine operation. Double-check all
wires disconnected or connected during any
wiring task to ensure tight connections.
WIRE/COMPONENT DAMAGE. Damaged wires
or components increase the risk of serious
personal injury, fire, or machine damage. If
you notice that any wires or components are
damaged while performing a wiring task,
replace those wires or components before
completing the task.
MODIFICATIONS. Using aftermarket parts or
modifying the wiring beyond what is shown
in the diagram may lead to unpredictable
results, including serious injury or fire.
MOTOR WIRING. The motor wiring shown
in these diagrams is current at the time
of printing, but it may not match your
machine. Always use the wiring diagram
inside the motor junction box.
CAPACITORS/INVERTERS. Some capacitors
and power inverters store an electrical
charge for up to 10 minutes after being
disconnected from the power source.
To reduce the risk of being shocked,
wait at least this long before working on
capacitors.
CIRCUIT REQUIREMENTS. You MUST follow
the requirements at the beginning of this
manual when connecting your machine to a
power source.
EXPERIENCING DIFFICULTIES. If you are
experiencing difficulties understanding
the information included in this section,
contact our Technical Support at
(360) 734-3482.
SERVICE
WIRING DIAGRAM COLOR KEY
The photos and diagrams
included in this section are
best viewed in color. You
can view these pages in
color at www.shopfox.biz.
BLACK
WHITE
GREEN
RED
BLUE
BROWN
GRAY
ORANGE
-33-
YELLOW
YELLOW
GREEN
PURPLE
PINK
LIGHT
BLUE
BLUE
WHITE
TURQUOISE
Page 36
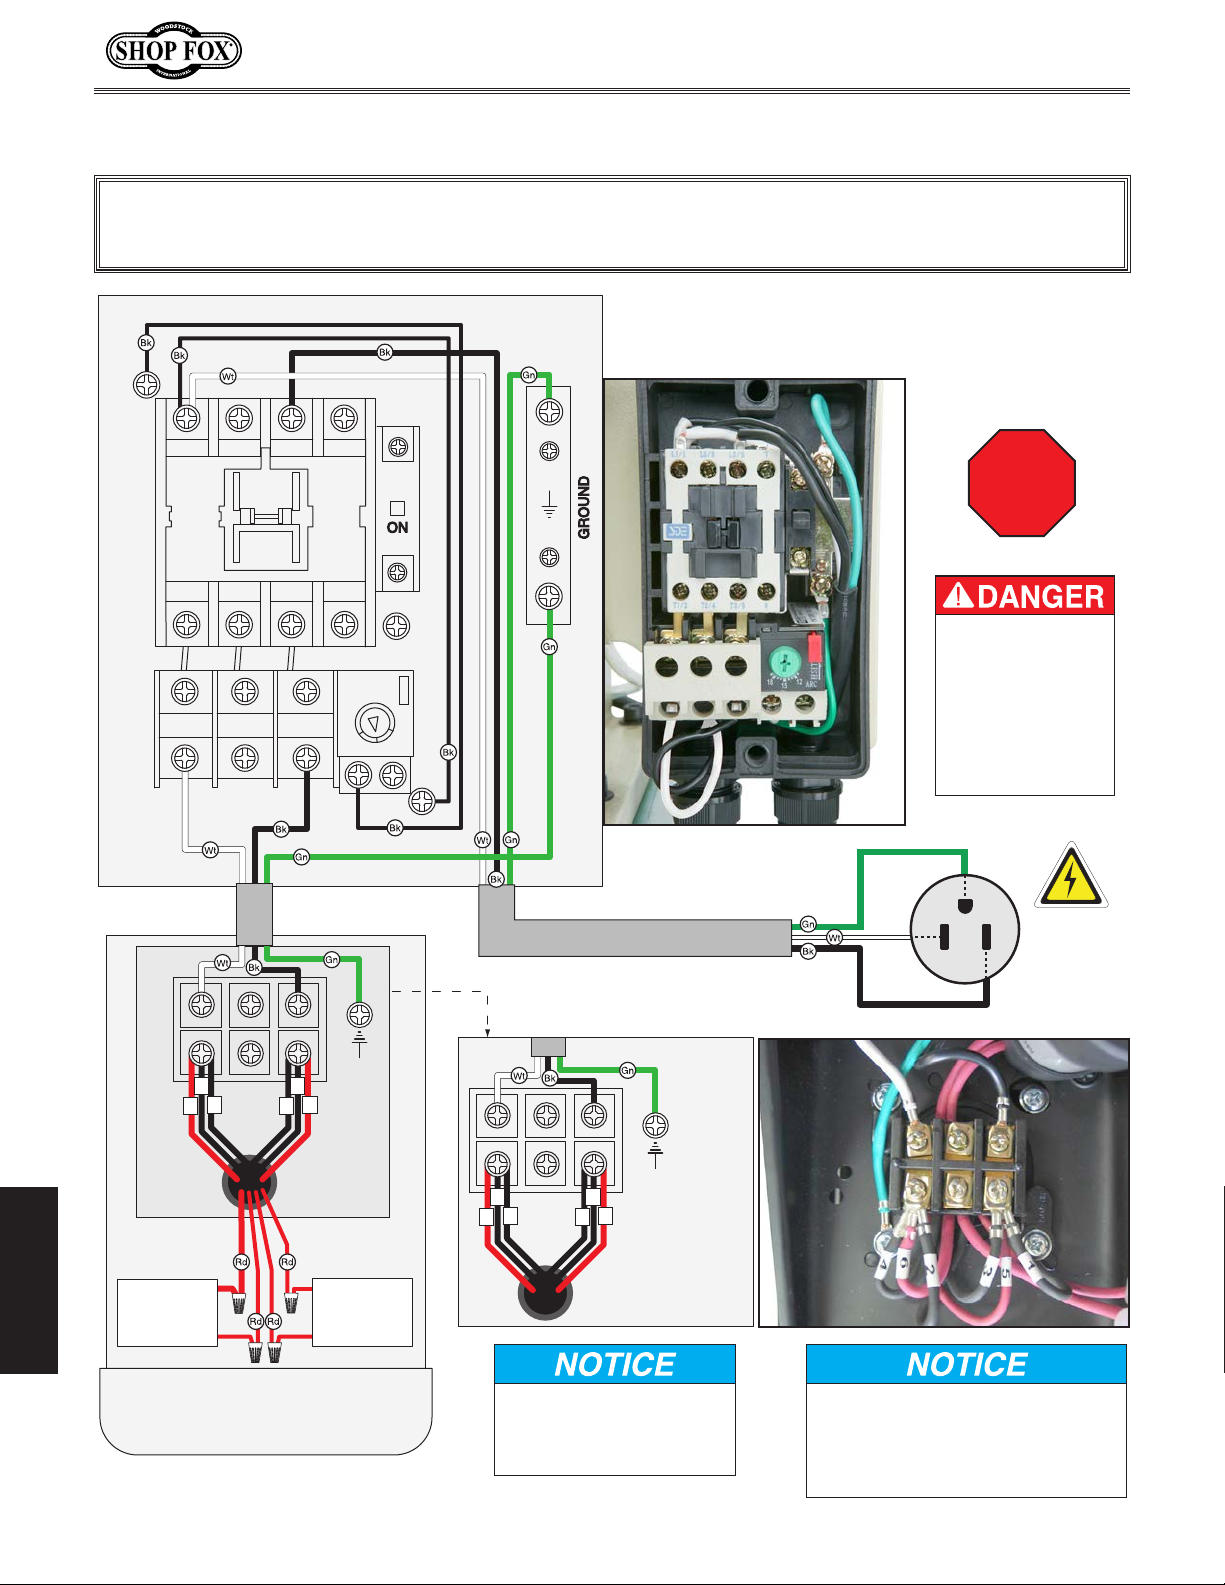
110V Wiring
Model W1805 (For Machines Mfd. Since 7/15)
110V Wiring Diagram
NOTICE
To convert to 110V, you must replace the magnetic switch assembly and rewire the motor.
MAGNETIC
SWITCH
A
ASSEMBLY
L1/1 L3/5 7L2/3
SDE
MA-18
T1/2 T3/6 8
T2/4
1/2
3/4
5/6
RA-20
18
96
AMP
Read
Page 33
STOP
Before
Wiring
B
Disconnect power
before servicing
electrical
RESET
OFF
12
15
98
95
White
Neutral
components.
Electrical shock
causes serious
personal injury or
even death!
Green
Ground
5-15 Plug
110 VAC
Black
Hot
4
2
6
3
5
1
CCW
Rotation
4
2
5
3
6
1
CW
Rotation
Start
Capacitor
SERVICE
300MFD
250VAC
Run
Capacitor
30MFD
250VAC
If your cutter rotates in
the wrong direction, wire
it for counterclockwise
(CCW) rotation.
MOTOR (Wired at 110V)
(for troubleshooting
purposes only)
The motor wiring shown here is
current at the time of printing;
however, always use the diagram on
the inside of junction box cover
when rewiring your motor.
-34-
Page 37
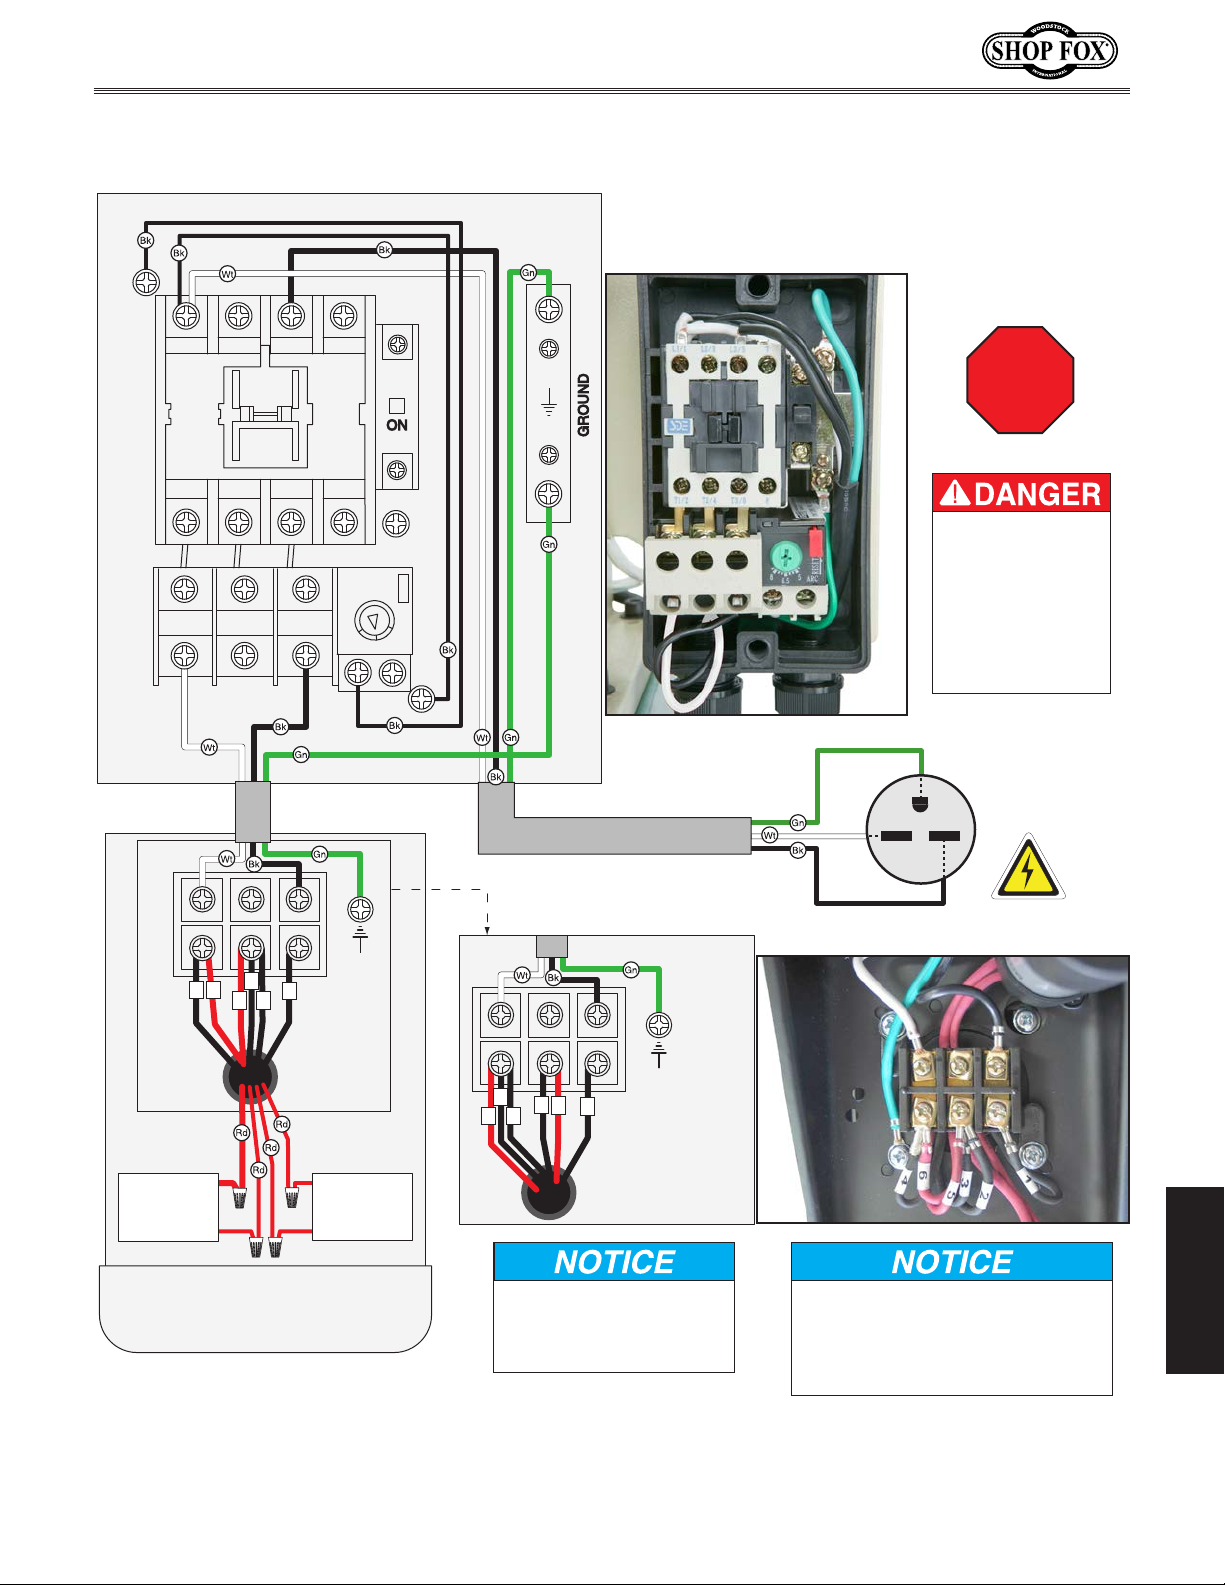
Model W1805 (For Machines Mfd. Since 7/15)
220V Wiring Diagram (Prewired)
A
220V Wiring
MAGNETIC
SWITCH
ASSEMBLY
L1/1 L3/5 7L2/3
SDE
MA-09
MA-15
T1/2 T3/6 8
T2/4
1/2
3/4
5/6
RA-20
96
Read
Page 33
STOP
Before
Wiring
B
Disconnect power
before servicing
AMP
RESET
OFF
5
8
6.5
98
95
Green
Ground
White
Hot
Black
Hot
electrical
components.
Electrical shock
causes serious
personal injury or
even death!
220
VAC
6-15 Plug
(As Recommended)
3
4
6
5 2
1
CCW
Rotation
Start
Capacitor
300MFD
250VAC
Capacitor
30MFD
250VAC
MOTOR (Wired at 220V)
Run
3
4
5
6 2
1
CW
Rotation
(for troubleshooting
purposes only)
If your cutter rotates in
the wrong direction, wire
it for counterclockwise
(CCW) rotation.
-35-
SERVICE
The motor wiring shown here is
current at the time of printing;
however, always use the diagram on
the inside of junction box cover
when rewiring your motor.
Page 38
The following troubleshooting tables cover common problems that may occur with this machine. If you
need replacement parts or additional troubleshooting help, contact our Technical Support.
Note:
Before contacting Tech Support, find the machine serial number and manufacture date, and if
available, your original purchase receipt. This information is required to properly assist you.
Motor & Electrical
PROBLEM POSSIBLE CAUSE CORRECTIVE ACTION
Machine does not
start or a breaker
trips.
Machine stalls or
is underpowered.
Machine has
vibration or noisy
operation.
SERVICE
Troubleshooting
1. STOP button pushed in, disabling the switch.
2. Plug/receptacle is at fault or wired incorrectly.
3. Start capacitor is at fault.
4. Motor connection wired incorrectly.
5. Power supply is at fault/switched OFF.
6. Motor ON button or ON/OFF switch is at
fault.
7. Motor centrifugal switch is at fault.
8. Emergency stop push-panel is stuck/switch is
at fault.
9. Motor windings or motor is at fault.
1. Wrong workpiece material (wood).
2. Feed rate too fast for task.
3. Run capacitor is at fault.
4. Belt slipping.
5. Motor connection is wired incorrectly.
6. Plug/receptacle is at fault.
7. Motor bearings are at fault.
8. Motor has overheated.
9. Motor is at fault.
10. Motor centrifugal switch is at fault.
1. Motor or component is loose.
2. Belt(s) worn or loose.
3. Motor fan is rubbing on fan cover.
4. Pulley is loose.
5. Machine is incorrectly mounted or sits unevenly on floor.
6. Cast iron motor mount loose/broken.
7. Motor or spindle bearings are at fault.
8. Cutter is at fault.
9. Motor centrifugal switch is at fault.
Model W1805 (For Machines Mfd. Since 7/15)
1. Twist STOP button clockwise until it pops out to
enable the switch.
2. Test for good contacts; correct the wiring.
3. Test/replace if faulty.
4. Correct motor wiring connections.
5. Ensure hot lines have correct voltage on all legs and
main power supply is switched ON.
6. Replace faulty ON button or ON/OFF switch.
7. Adjust/replace the centrifugal switch if available.
8. Free push-panel from binding; replace faulty
switch.
9. Replace motor.
1. Use wood with correct moisture content, without
glues, and little pitch/resins.
2. Decrease feed rate.
3. Tighten/repair/replace.
4. Replace bad belt and re-tension (see Page 32).
5. Correct motor wiring connections.
6. Test for good contacts; correct the wiring.
7. Test by rotating shaft; rotational grinding/loose
shaft requires bearing replacement.
8. Clean off motor, let cool, and reduce workload.
9. Test/repair/replace.
10. Adjust/replace centrifugal switch if available.
1. Inspect/replace stripped or damaged bolts/nuts,
and re-tighten with thread locking fluid.
2. Inspect/replace belts (refer to Page 32).
3. Replace dented fan cover; replace damaged fan.
4. Tighten pulley set screw.
5. Tighten/replace anchor studs in floor; relocate/
shim machine.
6. Tighten/replace.
7. Test by rotating shaft; rotational grinding/loose
shaft requires bearing replacement.
8. Replace warped, bent, or twisted cutter.
9. Adjust/replace centrifugal switch if available.
-36-
Page 39
Model W1805 (For Machines Mfd. Since 7/15)
Cutting Operations & Results
PROBLEM POSSIBLE CAUSE CORRECTIVE ACTION
Workpiece slips or kicks
out during operation.
Cutter cuts slow or does
not cut properly.
Dovetail joint fit is too
tight.
Dovetail joint fit is too
loose.
Tails fit too far into sockets.
Tails will not fit completely into the sockets.
Tails sit flush with pins
at one end but not the
oth er.
Gaps exist between tails
and pins.
Dado or groove for drawer bottom visible on
assembled joint.
Dovetails fit together
correctly, but tops/
edges of workpieces
are not flush with each
oth er.
Distribution of dovetails
across assembled joint is
not symmetrical.
1. Low air pressure to clamps.
2. Clamps are adjusted too far away from
the workpiece.
3. Clamp bracket is incorrectly adjusted,
causing the clamps to make uneven
contact with the workpiece.
1. Cutter is dull.
2. Belt is slipping on the pulley.
3. Cutter is rotating clockwise (motor is
wired incorrectly).
1. Cutter is not taking a large enough
cut.
1. Cutter is taking too large of a cut.
1. Sockets are cut too deep.
1. Cutter is not taking a large enough
cut.
2. Sockets are not cut deep enough.
1. Horizontal workpieces were not positioned square when clamped.
2. Horizontal workpieces were not cut
square or workpieces were not properly prepared.
1. Vertical workpieces were not positioned square when clamped.
2. The fixed chaser is not flush with the
horizontal table.
3. Vertical workpieces were not cut
square or workpieces were not properly prepared.
1. Dado cut in the wrong location for the
template being used.
2. Fences set incorrectly.
1. Fences were not offset by exactly half
of the template size being used.
1. Fences are not set correctly to allow
the cutter to start in the proper location.
2. Workpiece width is not divisible by the
template size being used.
1. Increase the air pressure to at least 40 PSI.
2. Adjust clamps closer to the workpiece (Page 20).
3. Adjust the both sides of the clamp bracket and even
distance from the table (Page 20).
1. Replace or sharpen the cutter (Page 31).
2. Tighten belt (Page 32) or replace belt (Page 32).
3. Wire motor so cutter rotates counterclockwise.
1. Adjust the cutter to take a larger cut (Page 29).
1. Adjust the cutter to take a smaller cut (Page 29).
1. Adjust the cutter depth stop so the cutter will not
cut as deeply into the horizontal workpiece (Page
26).
1. Adjust the cutter to take a larger cut (Page 29).
2. Adjust cutter depth stop so the cutter will cut
deeper into the horizontal workpiece (Page 26).
1. Reclamp the workpiece with emphasis on keeping it
square before and during clamping.
2. Cut new workpieces with emphasis on squaring up
all the boards (Page 18). Check the saw or technique used to cut the boards to ensure squareness.
1. Reclamp the workpiece with emphasis on keeping it
square before and during clamping.
2. Loosen the 3 cap screws securing the fixed chaser,
adjust it flush with horizontal table, and tighten.
3. Cut new workpieces with emphasis on squaring up
all the boards (Page 18). Check the saw or technique used to cut the boards to ensure squareness.
1. Cut dadoes in the correct location (Page 19).
2. Reset the fences (Page 22).
1. Set the fences so they are offset exactly half of
the distance as the template size being used. For
example, offset the fences
1
for 1
⁄2" template, etc. Refer to Page 22 for more
details.
1. Reset the fences, paying close attention to where
the first cut will be made into the vertical workpiece
(
Page 22).
2. Cut new workpieces that are divisible by template
size being used (Page 18); change template size to
be divisible by workpiece (
ter starting point by eye—results may not be truly
symmetrical.
1
⁄2" for 1" template, 3⁄4"
Page 21); or align cut-
SERVICE
-37-
Page 40
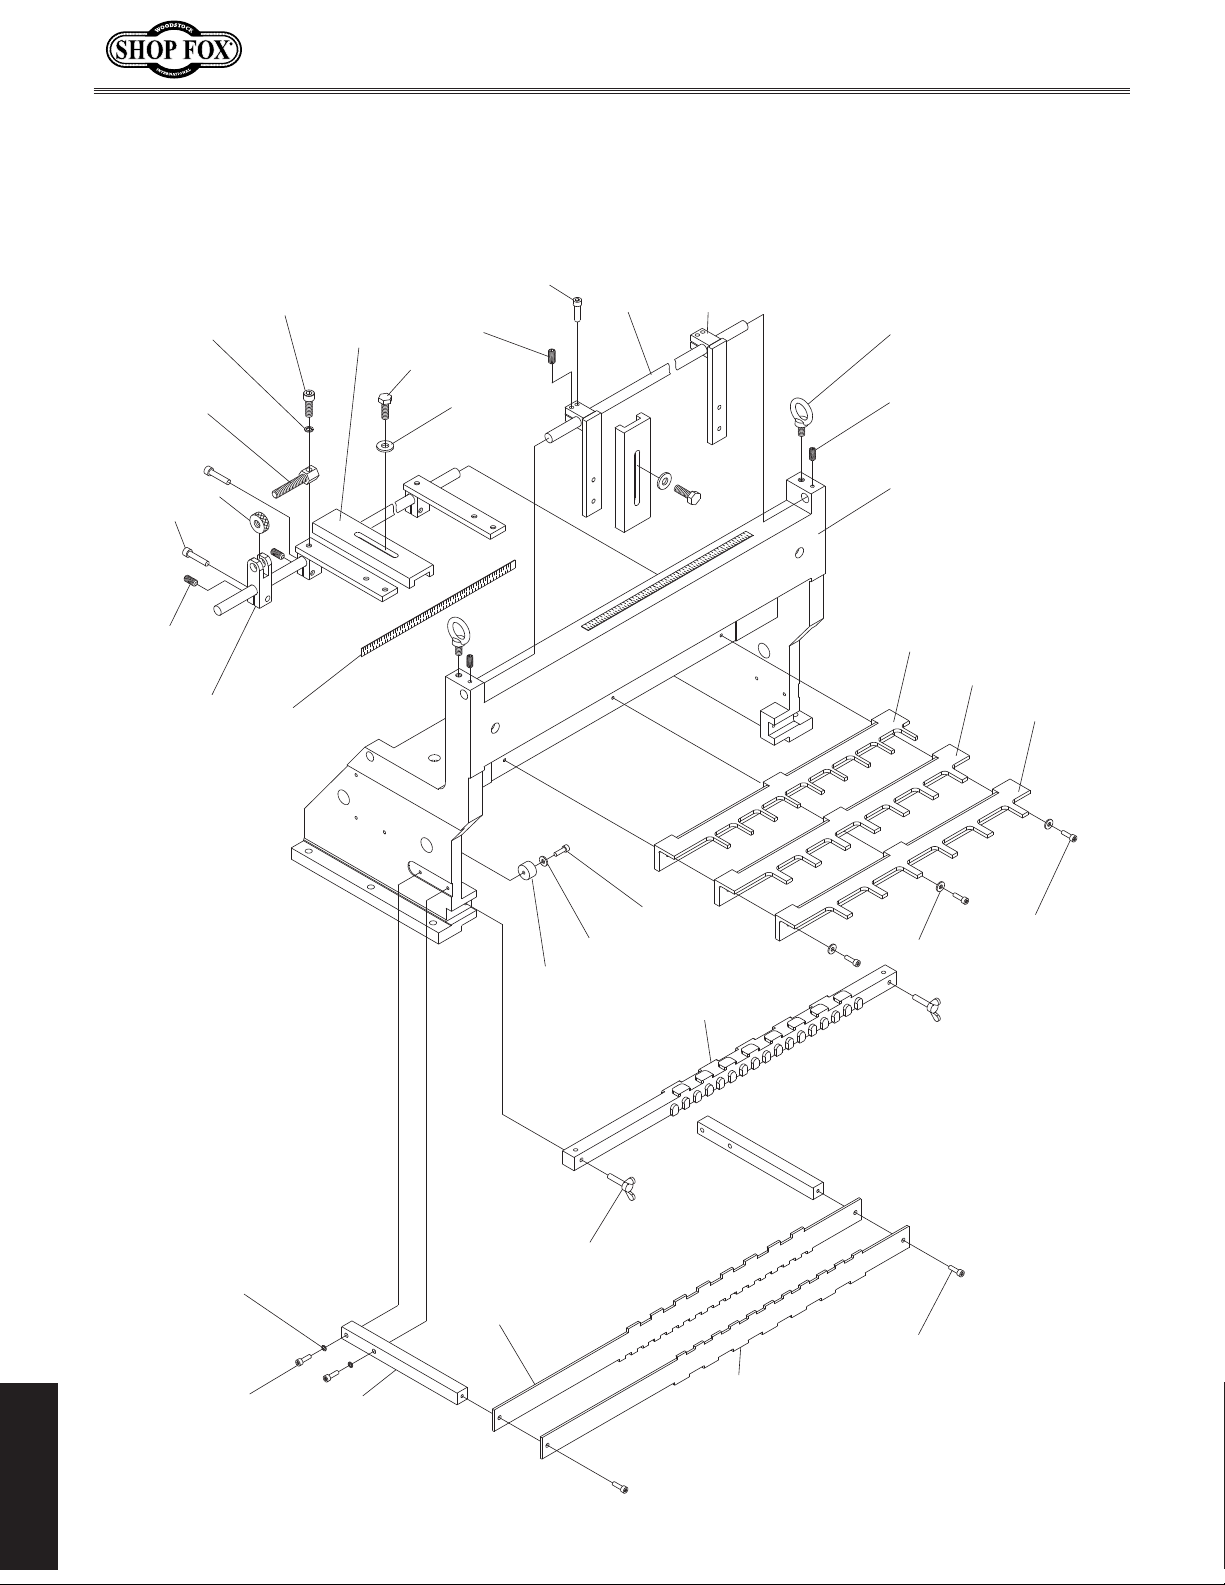
109
110
108
107
105
104
106
PARTS
Table
103
102
Model W1805 (For Machines Mfd. Since 7/15)
101
132
131
103
104
111
112
113
122
123
124
130
127
128
129
126
125
121
120
114
117
119
115
116
118
PARTS
-38-
Page 41
Model W1805 (For Machines Mfd. Since 7/15)
Table Parts List
REF PART # DESCRIPTION REF PAR T # DESCR IPTION
101 X1805101 FENCE 117 X1805117 INDICATOR TEMPLATE 1" & 2"
102 X1805102 SLIDING ROD 118 X1805118 INDICATOR TEMP LATE 1-1/2" & 2-1/2"
103 X1805103 CAP SCREW M8-1.25 X 25 119 X1805119 CAP SCREW M6-1 X 10
104 X1805104 SET SCREW M6-1 X 12 120 X1805120 WING SCR EW M6- 1 X 35
105 X1805105 HEX BOLT M8-1.25 X 20 121 X1805121 TEMP LATE BAR
106 X1805106 FLAT W ASHER 8MM 122 X1805122 BUFFER P AD
107 X1805107 BUFFER P AD 123 X1805123 FLAT W ASHER 6MM
108 X1805108 CAP SCREW M8-1.25 X 30 124 X1805124 CAP SCREW M6-1 X 20
109 X1805109 LOC K W AS HER 8MM 125 X1805125 FLAT W ASHER 6MM
110 X1805110 ADJUSTMENT SCREW 126 X1805126 CAP SCREW M6-1 X 30
111 X1805111 ADJUSTMENT NUT 127 X1805127 FIX ED CH AS ER 2"
112 X1805112 MICRO-ADJUSTMENT SEAT 128 X1805128 FIX ED CHASER 3"
113 X1805113 TABLE SCALE 129 X1805129 FI XED CH ASER 2-1/2"
114 X1805114 LOCK WASH ER 6MM 130 X 1805130 WO RK TABLE
115 X1805115 CAP S CREW M6-1 X 35 131 X1805131 SET SCREW M6-1 X 6
116 X1805116 I NDICAT OR MOUNT ING BA R 132 X1805132 EY E BOLT M10-1.5 X 15
-39-
PARTS
Page 42
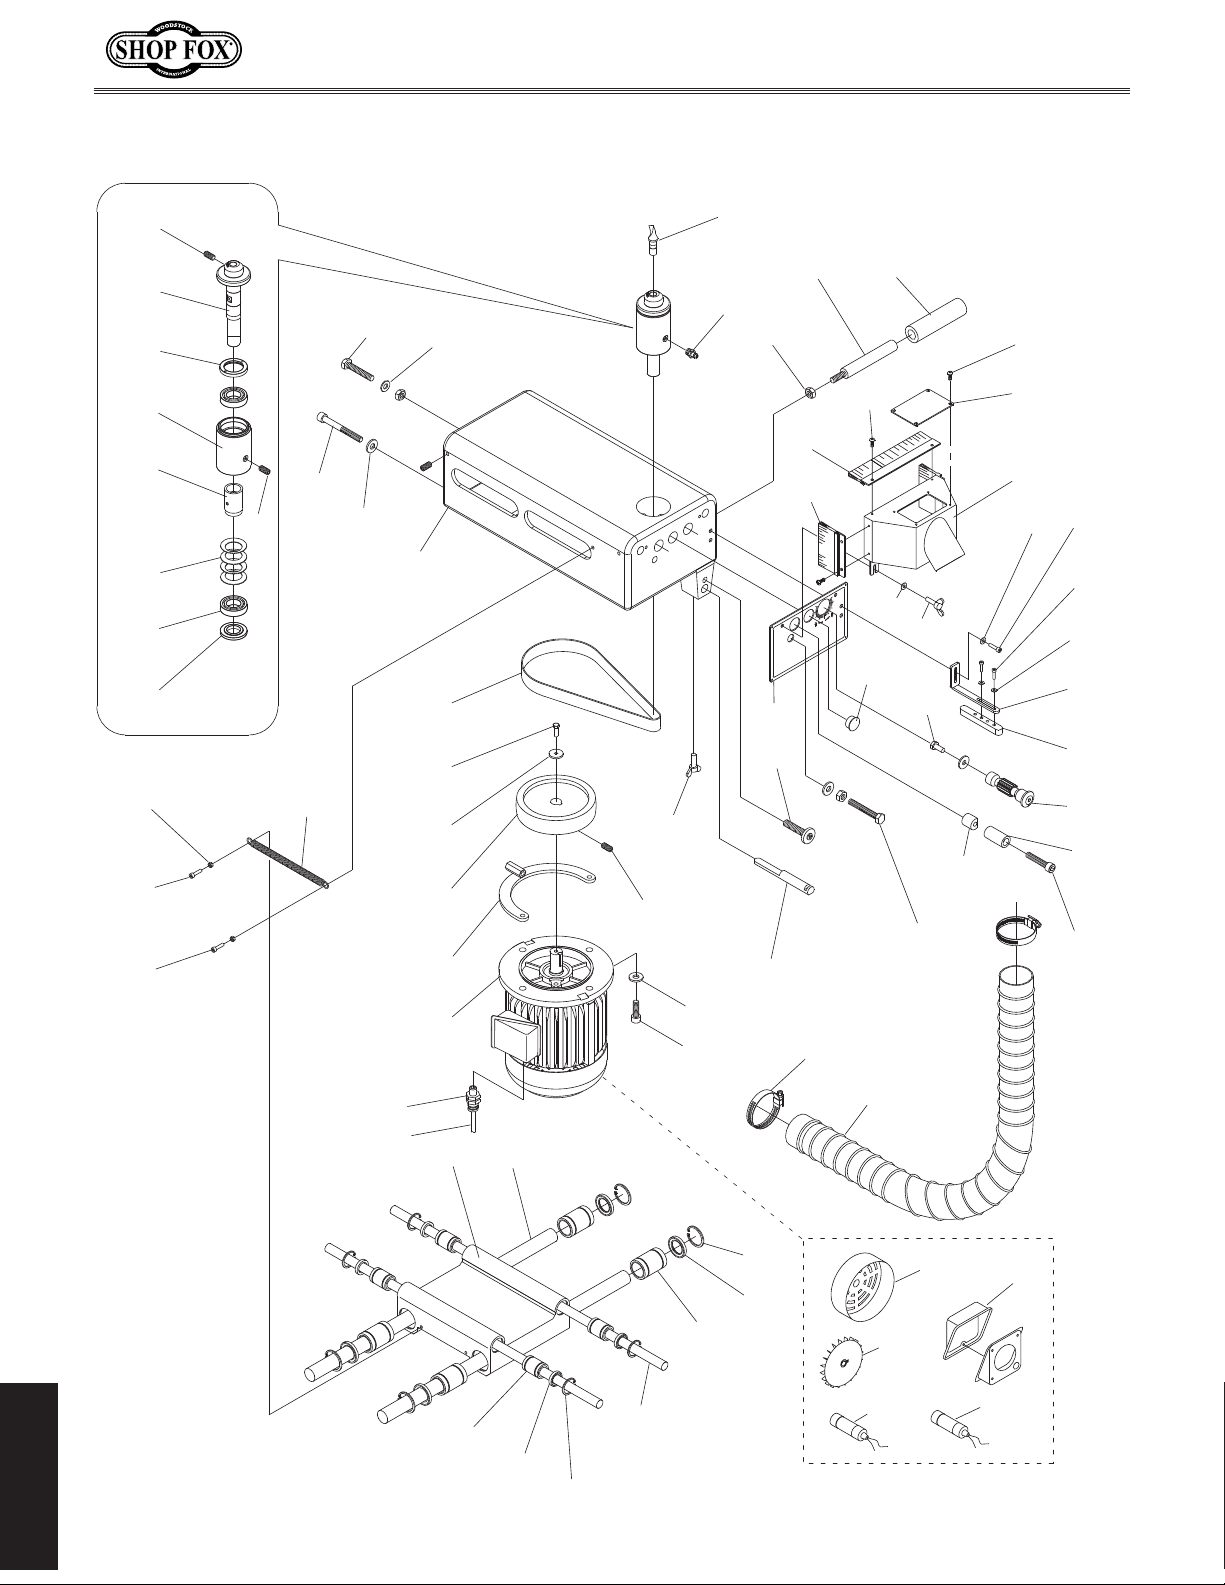
Model W1805 (For Machines Mfd. Since 7/15)
235
Headstock
211
212
213
214
215
217
218
219
220
221
222
216
214A
210
223
209
207
208
224
225
226
227
228
206
245
244
205
204
202 201
203
260-1
260-2
263
246
243
262
247
259
264
248
249
250
262
261
260
259
258
257
256
255
254
253
252
251
209
242
237
239
238
241
240
229-2
229-4
229-1
229-3
229-5
230
230-1
229
231
233
232
236
234
PARTS
-40-
Page 43
Model W1805 (For Machines Mfd. Since 7/15)
Headstock Parts List
REF PART # DESCRIPTION REF PART # DESCRIPTION
201 X1805201 SPONGE COATI NG 231 X1805231 CARRIAGE
202 X1805202 H ANDLE 232 X1805232 GUIDE ROD M25 X 750L
203 X1805203 H EX NUT M10-1.5 233 X1805233 LINEAR BUSHING 16UU
204 X1805204 GREASE FITTING M6-1 x 5 234 X1805234 SEAL 16 X 28 X 7 X 3
205 X1805205 CUTTER 235 X 1805235 INT RET AINING RING 28MM
206 X1805206 FLAT WASH ER 10MM 236 X1805236 GUIDE ROD M16 X 459L
207 X1805207 H EX B OLT M10-1. 5 X 80 237 X1805237 LINEAR BUSHING 25UU
208 X1805208 SPINDLE S LIDE SEAT 238 X1805238 SEAL 25 X 40 X 7 X 2
209 X1805209 FLAT WASHER 8MM 239 X1805239 I NT RETAINING RING 40MM
210 X1805210 CAP SCREW M8-1.25 X 100 240 X1805240 FLEXIB LE HOSE 2.5" X 63"
211 X1805211 SET SCREW M8-1.25 X 10 241 X1805241 H OSE CLAMP 2-3/4"
212 X1805212 ECCENTR IC SP INDLE 242 X1805242 CAP SCREW M8-1.25 X 35
213 X1805213 LOCK NUT 243 X1805243 TRACER PIN
214 X1805214 SPINDLE BEARING HOUSING 244 X1805244 SET SCREW M5-.8 X 12
214A X 1805214A COMPLETE SPINDLE ASSY 245 X1805245 W ING SCREW M6-1 X 20
215 X1805215 SPACER 246 X1805246 ADJUSTMENT SCREW
216 X1805216 SET SCREW M5-.8 X 5 247 X 1805247 PLASTIC PLUG 22MM
217 X1805217 COMPRESSION SPRING AK-6005 248 X1805248 H EX B OLT M8-1. 25 X 16
218 X1805218 B ALL B EARING 6005 249 X1805249 CAP SCREW M10-1.5 X 150
219 X1805219 FI XING NUT 250 X1805250 CLAMP BUS HING
220 X1805220 HEX NUT M5-.8 251 X1805251 CAP SCREW M8-1.25 X 65
221 X1805221 CAP SCREW M5-.8 X 35 252 X1805252 B USHI NG
222 X1805222 CAP SCREW M5-.8 X 20 253 X1805253 GEAR SHAFT
223 X1805223 EX TENSION SPRING 254 X 1805254 INDICATOR BAR
224 X1805224 FLAT BELT 670 X 25 255 X1805255 INDICATOR BRACKET
225 X1805225 H EX B OLT M6-1 X 20 256 X1805256 FLAT WASHER 4MM
226 X1805226 FLAT WASHER 6MM 257 X1805257 CAP SCREW M4-.7 X 10
227 X1805227 MOTOR PULLEY 258 X 1805258 CAP SCREW M5- .8 X 12
228 X1805228 MOTOR BRACKET 259 X1805259 FLAT WASHER 5MM
229 X1805229 MOTOR 1HP, 110V/220V 260 X1805260 G UAR D W ITH BRUS H
229-1 X1805229-1 MOTOR FAN COVER 260-1 X1805260-1 T OP G UAR D B RUSH
229-2 X1805229-2 MOTOR FAN 260-2 X1805260-2 SIDE GUARD BRUSH
229-3 X1805229-3 MOTOR JUNCTION BOX 261 X1805261 WINDOW
229-4 X1805229-4 S CAPACITOR 300MFD 250VAC 262 X1805262 P HLP HD SCR M4-. 7 X 6
229-5 X1805229-5 R CAPACITOR 30MFD 250VAC 263 X1805263 CONTROL PANEL LABEL
230 X1805230 STRAIN RELIEF 11-10B 264 X 1805264 WING SCREW M5-.8 X 15
230-1 X1805230-1 MOTOR CORD
-41-
PARTS
Page 44
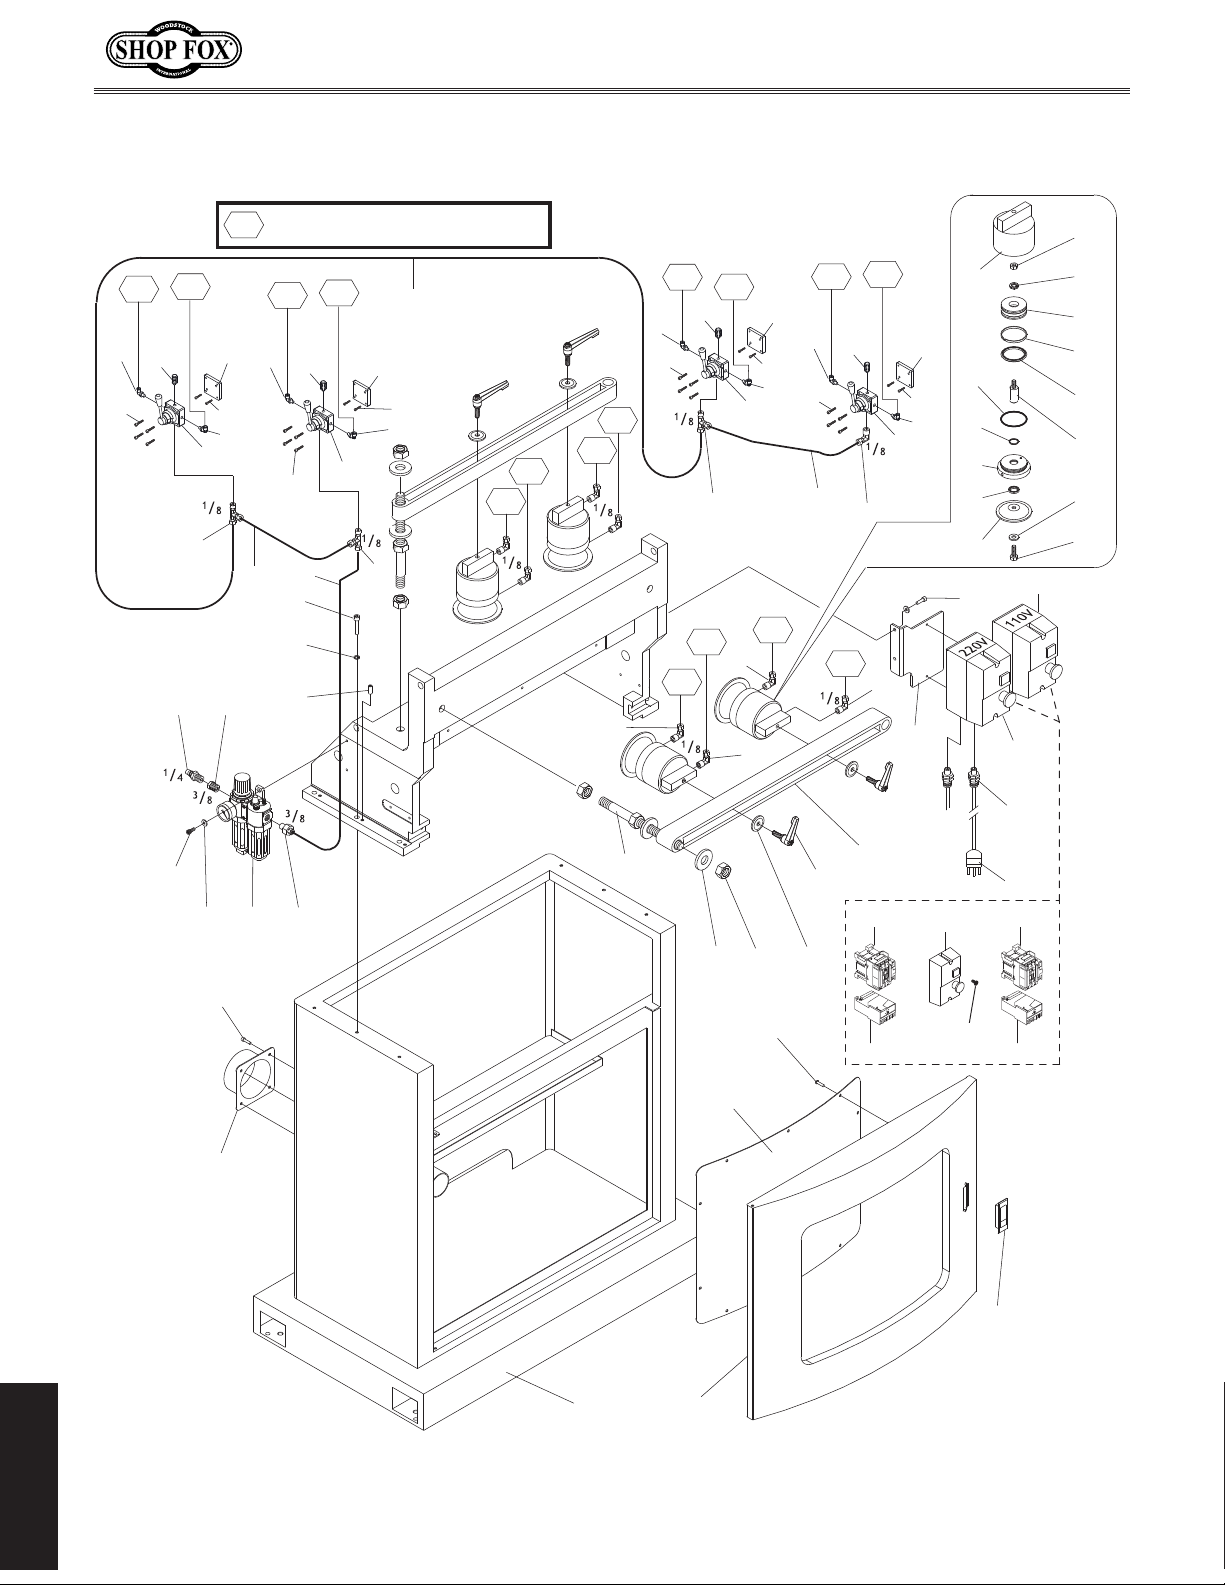
=
AIR TUBE CONNECTION POINT
Model W1805 (For Machines Mfd. Since 7/15)
Stand
347
332
348
409
349
410
350
351
332
301V2
305
310 309
332
402
405
348
401
306
307
308
349
406
301V2
350
305
403
351
332
410
409
412
332
411
332
348
412
405
349
305
406
411
332
350
351
332
301V2
407
332
332
348
404
408
349
408
332
407
332
350
351
332
301V2
331
334
335
336
337
338
339
311
346
345
344
343
342
341
340
330A
330
329
311
312
315
316
313
314
317
322
318
323
320
326
324 325
321
327
330-1
330-2
330-3
330-4
328
330A-1
330A-2
319
PARTS
-42-
Page 45
Model W1805 (For Machines Mfd. Since 7/15)
330A-2 X1805330A -2 O VERLO AD RELAY FO R 110V
Stand Parts List
REF PAR T # DESCRIPTION REF PAR T # DESCRIPTION
301V2 X 1805301V2 CONTROL VA LVE V2. 07.15 331 X 1805331 SWITCH BRACKET
305 X 1805305 T- CONNECTOR P T- 1/8" X 6MM X 6MM 332 X1805332 MALE ELB OW PT 1/8" X 6MM
306 X 1805306 CAP SCR EW M8- 1.25 X 35 333 X 1805333 CAP SCR EW M5- .8 X 50
307 X 1805307 LOCK W ASHER 8MM 334 X 1805334 CYLI NDER BODY
308 X 1805308 SET SCREW M8-1. 25 X 10 335 X 1805335 O-RING G80
309 X 1805309 ADAPTER 3/8" X 1/4" 336 X 1805336 O-RING P25
310 X 1805310 MALE COUPLI NG PT-1/4" 337 X 1805337 CY LINDER END COVER
311 X 1805311 CAP SCR EW M6- 1 X 16 338 X 1805338 LOCKI NG P IECE
312 X 1805312 FLAT WASHER 6MM 339 X1805339 CLAMPING DISC
313 X 1805313 AIR SUPPLY UNIT MACP 300- 10A 340 X 1805340 HEX BO LT M8- 1.25 X 16
314 X 1805314 MALE CONNECTOR PT-3/8" X 6MM 341 X 1805341 FLAT WASHER 8MM
315 X 1805315 CAP SCR EW M5- .8 X 10 342 X 1805342 PISTON ROD
316 X 1805316 DUST PORT 4" 343 X 1805343 PI STO N BACKING 80 X 65 X 5.5
317 X 1805317 CABI NET 344 X1805344 WEARING 80 X 75 X 6
318 X 1805318 DOOR 345 X 1805345 PISTON
319 X 1805319 DOOR LATCH 346 X 1805346 LOC K WASH ER 12MM
320 X 1805320 DOOR INSET 347 X1805347 HEX NUT M12-1. 75
321 X 1805321 PH LP HD S CR M5- .8 X 6 348 X 1805348 CAP SCREW M5-.8 X 30
322 X 1805322 STUD 349 X 1805349 AIR DIFFUSER 1/8" NPT
323 X 1805323 FLAT WASHER 20MM 350 X 1805350 MO UNTI NG P LATE
324 X 1805324 HEX NUT M20-2.5 351 X 1805351 CAP SCREW M5-.8 X 20
325 X 1805325 SP ECI AL W AS HER 401 X 1805401 PU TUBE 4 X 6 X 240MM
326 X 1805326 LOC KING HANDLE M10-1.5 X 35 402 X 1805402 PU TUBE 4 X 6 X 140MM
327 X 1805327 HOLDER BRACKET 403 X 1805403 PU TUBE 4 X 6 X 1360MM
328 X 1805328 POWER CORD 404 X1805404 PU TUB E 4 X 6 X 140MM
329 X 1805329 STRAIN RELIEF MG B20G-12B 405 X 1805405 PU TUBE 4 X 6 X 790MM
330 X 1805330 MAGNETIC SWITCH ASSY 220V 406 X 1805406 PU TUBE 4 X 6 X 730MM
330A X 1805330A MAGNETIC SWITCH ASSY 110V 407 X 1805407 P U TUBE 4 X 6 X 790MM
330-1 X1805330-1 CONTACT OR 220V 408 X 1805408 PU TUBE 4 X 6 X 730MM
330-2 X1805330-2 OV ERLOA D RELAY FOR 220V 409 X 1805409 PU TUBE 4 X 6 X 790MM
330-3 X1805330-3 MAG SWITCH COVER 410 X 1805410 P U TUBE 4 X 6 X 730MM
330-4 X1805330-4 PLASTIC SCREW 411 X 1805411 PU TUBE 4 X 6 X 790MM
330A-1 X1805330A -1 CONTACTOR 110V 412 X 1805412 PU TUBE 4 X 6 X 730MM
PARTS
-43-
Page 46
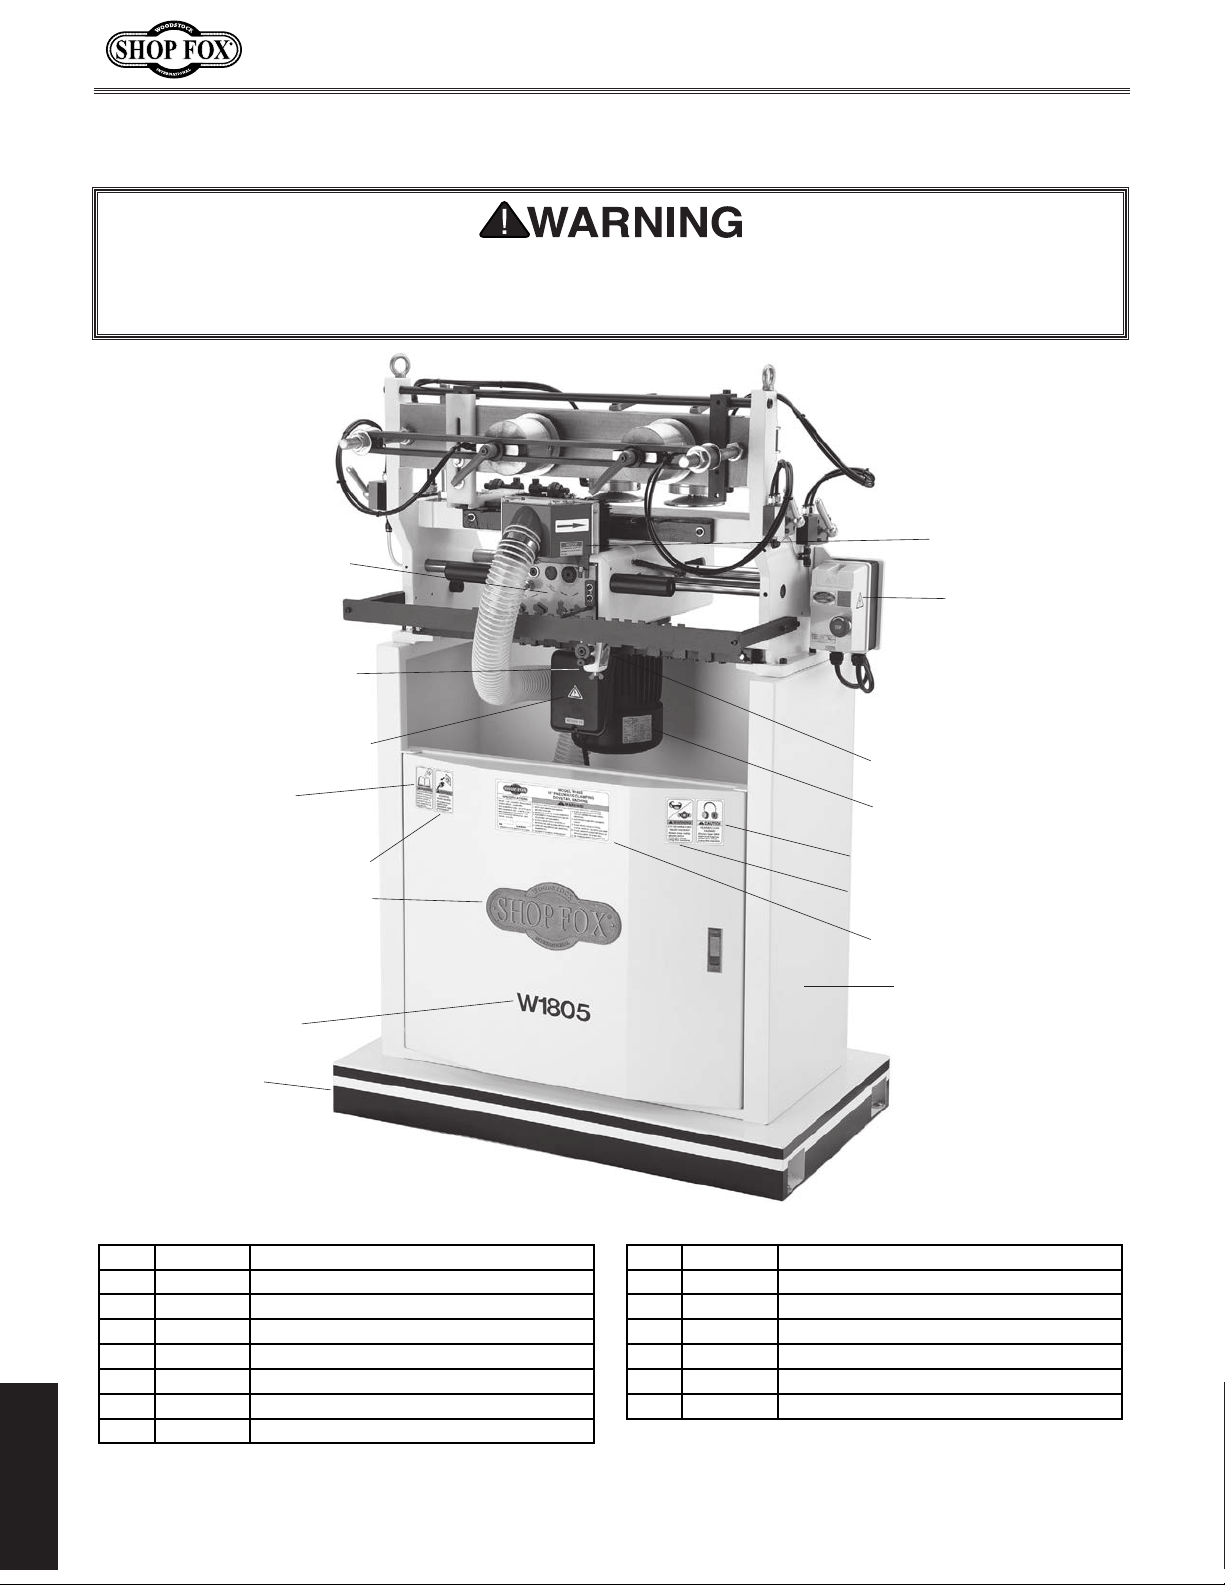
Safety labels warn about machine hazards and how to prevent serious personal injury. The owner
of this machine MUST maintain the original location and readability of all labels on this machine.
If any label is removed or becomes unreadable, REPLACE that label before allowing machine to
be operated again. Contact us at (360) 734-3482 or www.woodstockint.com to order new labels.
505
Model W1805 (For Machines Mfd. Since 7/15)
Label Placement
513
511
512
511
502
509
506
504
508
501
503
515
514
510
507
REF PART # DESCRIPTION REF PART # DESCRIPTION
501 X1805501 TAIL SHORTER LABEL 509 X 1805509 DISCONNEC T P OW ER LAB EL
502 X1805502 READ MANUAL LABEL 510 X1805510 MA CH INE I D LABEL
503 X1805503 MOTOR LABEL 511 X1805511 ELECTRICI TY LABEL
504 X1805504 MO DEL # LABEL 512 X1805512 TAIL LONGER LABEL
505 X1805505 CONTROL PANEL LABEL 513 X1805513 GREAS E SP INDLE LABEL
506 X1805506 SHOP FOX LOGO PLATE 514 X 1805514 RESPIRATOR/GLASSES LABEL
507 X1805507 SH OP FOX OFF-WHITE PAINT 515 X 1805515 EA R P RO TECTION LA BEL
508 X1805508 DECORATIVE STRIPE
PARTS
-44-
Page 47
warranty does not apply to defects due directly or indirectly to misuse, abuse, negligence or accidents,
WARRANTY
WARRANTY
Woodstock International, Inc. warrants all Shop Fox machinery to be free of defects from workmanship
and materials for a period of two years from the date of original purchase by the original owner. This
lack of maintenance, or reimbursement of third party expenses incurred.
Woodstock International, Inc. will repair, replace, or arrange for a dealer refund, at its expense and
option, the Shop Fox machine or machine part proven to be defective for its designed and intended
use, provided that the original owner returns the product prepaid to an authorized warranty or repair
facility as designated by our Bellingham, Washington office with proof of their purchase of the product
within two years, and provides Woodstock International, Inc. reasonable opportunity to verify the
alleged defect through inspection. If it is determined there is no defect, or that the defect resulted
from causes not within the scope of Woodstock International Inc.'s warranty, then the original owner
must bear the cost of storing and returning the product.
This is Woodstock International, Inc.’s sole written warranty and any and all warranties that may be
implied by law, including any merchantability or fitness, for any particular purpose, are hereby limited
to the duration of this written warranty. We do not warrant that Shop Fox machinery complies with
the provisions of any law, acts or electrical codes. We do not reimburse for third party repairs. In no
event shall Woodstock International, Inc.’s liability under this limited warranty exceed the purchase
price paid for the product, and any legal actions brought against Woodstock International, Inc. shall be
tried in the State of Washington, County of Whatcom. We shall in no event be liable for death, injuries
to persons or property or for incidental, contingent, special or consequential damages arising from the
use of our products.
Every effort has been made to ensure that all Shop Fox machinery meets high quality and durability
standards. We are commited to continuously improving the quality of our products, and reserve the
right to change specifications at any time.
To register the warranty, go to https://www.woodstockint.com/warranty, or scan the QR code below.
You will be directed to the Warranty Registration page on www.woodstockint.com. Enter all applicable
production information.
WARRANTY
WOODSTOCKINT.COM
Page 48
 Loading...