

Page 1
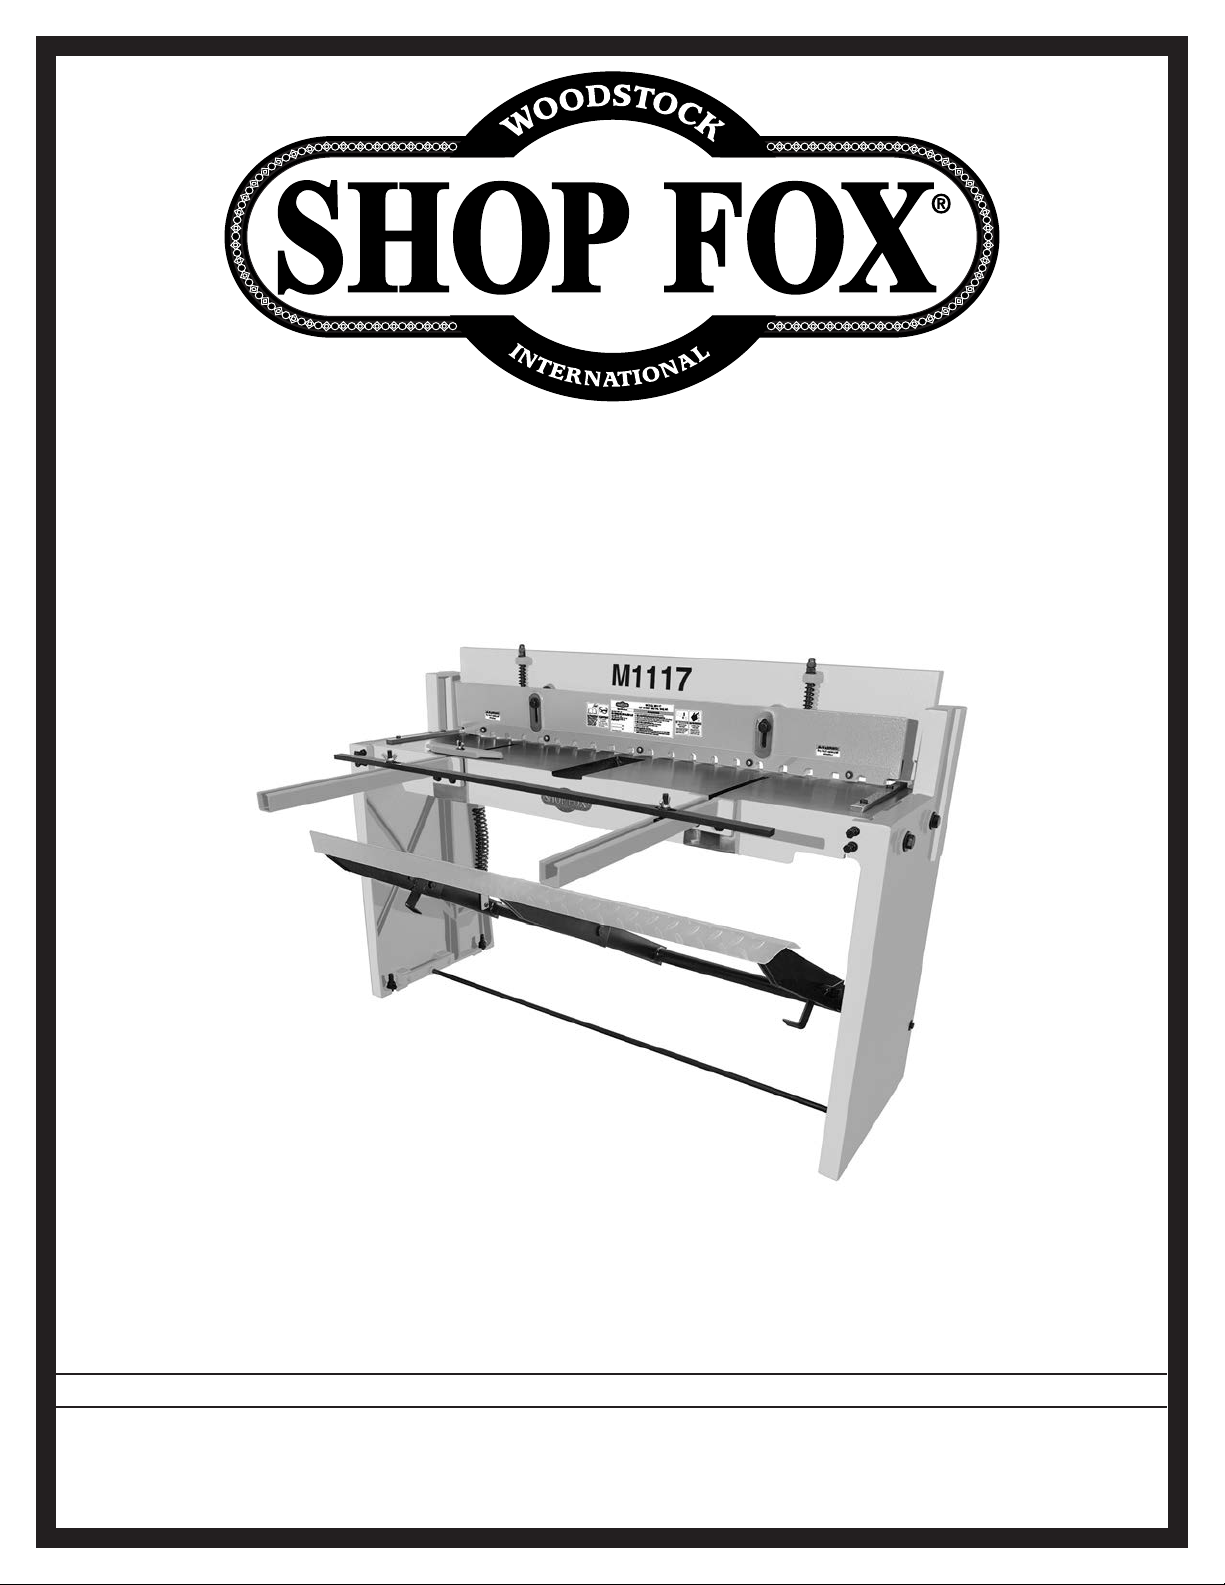
MODEL M1117
52" SHEET METAL SHEAR
OWNER'S MANUAL
(FOR MODELS MANUFACTURED SINCE 9/21)
Phone: (360) 734-3482 • Online Technical Support: [email protected]
COPYRIGHT © SEPTEMBER, 2021 BY WOODSTOCK INTERNATIONAL, INC.
WARNING: NO PORTION OF THIS MANUAL MAY BE REPRODUCED IN ANY SHAPE OR FORM WITHOUT
V1.09.21
THE WRITTEN APPROVAL OF WOODSTOCK INTERNATIONAL, INC.
#22053CS Printed in China
Page 2
This manual provides critical safety instructions on the proper setup,
operation, maintenance, and service of this machine/tool. Save this
document, refer to it often, and use it to instruct other operators.
Failure to read, understand and follow the instructions in this manual
may result in fire or serious personal injury—including amputation,
electrocution, or death.
The owner of this machine/tool is solely responsible for its safe use.
This responsibility includes but is not limited to proper installation in
a safe environment, personnel training and usage authorization,
proper inspection and maintenance, manual availability and comprehension, application of safety devices, cutting/sanding/grinding tool
integrity, and the usage of personal protective equipment.
The manufacturer will not be held liable for injury or property
damage from negligence, improper training, machine modifications or
misuse.
Some dust created by power sanding, sawing, grinding, drilling, and
other construction activities contains chemicals known to the State of
California to cause cancer, birth defects or other reproductive harm.
Some examples of these chemicals are:
• Lead from lead-based paints.
• Crystalline silica from bricks, cement and other masonry products.
• Arsenic and chromium from chemically-treated lumber.
Your risk from these exposures varies, depending on how often you
do this type of work. To reduce your exposure to these chemicals:
Work in a well ventilated area, and work with approved safety equipment, such as those dust masks that are specially designed to filter
out microscopic particles.
Page 3
Contents
INTRODUCTION .....................................2
Woodstock Technical Support
Machine Specifications
Identification
Controls & Components
SAFETY ............................................... 6
Standard Machinery Safety Instructions
Additional Safety for Metal Shears
SETUP ................................................ 9
Unpacking
Items Needed for Setup
Hardware Recognition Chart
Inventory
Cleaning Machine
Machine Placement
Lifting & Placing................................ 14
Anchoring to Floor
Assembly
OPERATIONS....................................... 19
Operation Overview
Cutting Tips
Adjusting Rear Work Stop
Adjusting Front Work Stop
Using Bevel Gauge
..................................... 4
......................................... 9
........................................ 11
......................................... 16
..................................... 20
.......................... 3
............................... 12
............................ 13
............................. 15
........................... 19
............................. 21
.................. 2
......................... 5
...... 6
............ 8
......................... 9
................. 10
..................... 20
.................... 21
ACCESSORIES ...................................... 22
Metal Shear Accessories
MAINTENANCE .................................... 24
General
Cleaning & Protecting
Lubrication
SERVICE ............................................ 27
General
Adjusting Gibs
Sharpening/Replacing Blade
Adjusting Blade Gap
Adjusting Blade Bow
Adjusting Return Spring Tension
Squaring Front Scales
Adjusting Hold-Down/Blade Guard
Troubleshooting
PARTS .............................................. 34
Main
Labels & Cosmetics
WARRANTY ........................................ 37
.......................................... 24
...................................... 25
.......................................... 27
.................................. 27
................................. 33
.............................................. 34
....................... 22
......................... 24
.................. 28
........................... 29
........................... 30
............. 31
.......................... 31
.......... 32
............................ 36
SAFETYINTRODUCTION
SETUPELECTRICAL MAINTENANCE
OPERATIONS
USE THE QUICK GUIDE PAGE LABELS TO SEARCH OUT INFORMATION FAST!
SERVICE PARTS
Page 4
Model M1117 (For Machines Mfd. Since 9/21)
INTRODUCTION
INTRODUCTION
Woodstock Technical Support
This machine has been specially designed to provide many years of trouble-free service. Close attention
to detail, ruggedly built parts and a rigid quality control program assure safe and reliable operation.
Woodstock International, Inc. is committed to customer satisfaction. Our intent with this manual is to
include the basic information for safety, setup, operation, maintenance, and service of this product.
We stand behind our machines! In the event that questions arise about your machine, please
contact Woodstock International Technical Support at (360) 734-3482 Ext. 2 or send e-mail to:
[email protected]. Our knowledgeable staff will help you troubleshoot problems and process warranty claims.
If you need the latest edition, you can download it from http://www.woodstockint.com/manuals.
If you have comments about this manual, please contact us at:
Woodstock International, Inc.
Attn: Technical Documentation Manager
P.O. Box 2309
Bellingham, WA 98227
Email: [email protected]
-2-
Page 5
Model M1117 (For Machines Mfd. Since 9/21)
MODEL M1117
52" SHEET METAL SHEAR
Product Dimensions
Weight.......................................................................................................... 982 lbs.
Width (side‐to‐side) x Depth (front‐to‐back) x Height........................................ 62 x 74 x 42 in.
Footprint (Length x Width).............................................................................. 60 x 21 in.
Shipping Dimensions
Type....................................................................................................... Wood Crate
Content........................................................................................................ Machine
Weight........................................................................................................ 1120 lbs.
Length x Width x Height........................................................................... 67 x 30 x 46 in.
Must Ship Upright.................................................................................................. Yes
INTRODUCTION
Main Specifications
Capacities
Maximum Width.......................................................................................... 52 in.
Maximum Thickness Mild Steel.................................................................... 16 Gauge
Maximum Thickness at Half Width Mild Steel................................................... 14 Gauge
Maximum Thickness at Full Width Mild Steel.................................................... 16 Gauge
Aluminum............................................................................................. 12 Gauge
Soft Brass............................................................................................. 14 Gauge
Annealed Phosphor Bronze......................................................................... 17 Gauge
Soft Copper........................................................................................... 14 Gauge
Hard Copper.......................................................................................... 14 Gauge
ABS Plastic............................................................................................... 2.2mm
Stainless Steel........................................................................................ 20 Gauge
Maximum Beam Lift.................................................................................. 1‐3/4 in.
Bed Height Above Floor............................................................................ 42‐1/8 in.
Working Height...................................................................................... 31‐1/4 in.
Front Stop Scale Range........................................................................ 0 ‐ 12‐1/2 in.
Rear Stop Scale Range............................................................................... 0 ‐ 33 in.
Construction
Frame....................................................................................................... Steel
Head and Tail Supports.................................................................................. Steel
Shear Table........................................................................................... Cast Iron
Shear Hold‐Down Clamp............................................................................. Cast Iron
Shear Blades................................................................................. 9CrSi Alloy Steel
Other
Country of Origin ............................................................................................... China
Warranty ....................................................................................................... 2 Years
Approximate Assembly & Setup Time ................................................................. 30 Minutes
Serial Number Location .......................................................................... Machine ID Label
-3-
Page 6
INTRODUCTION
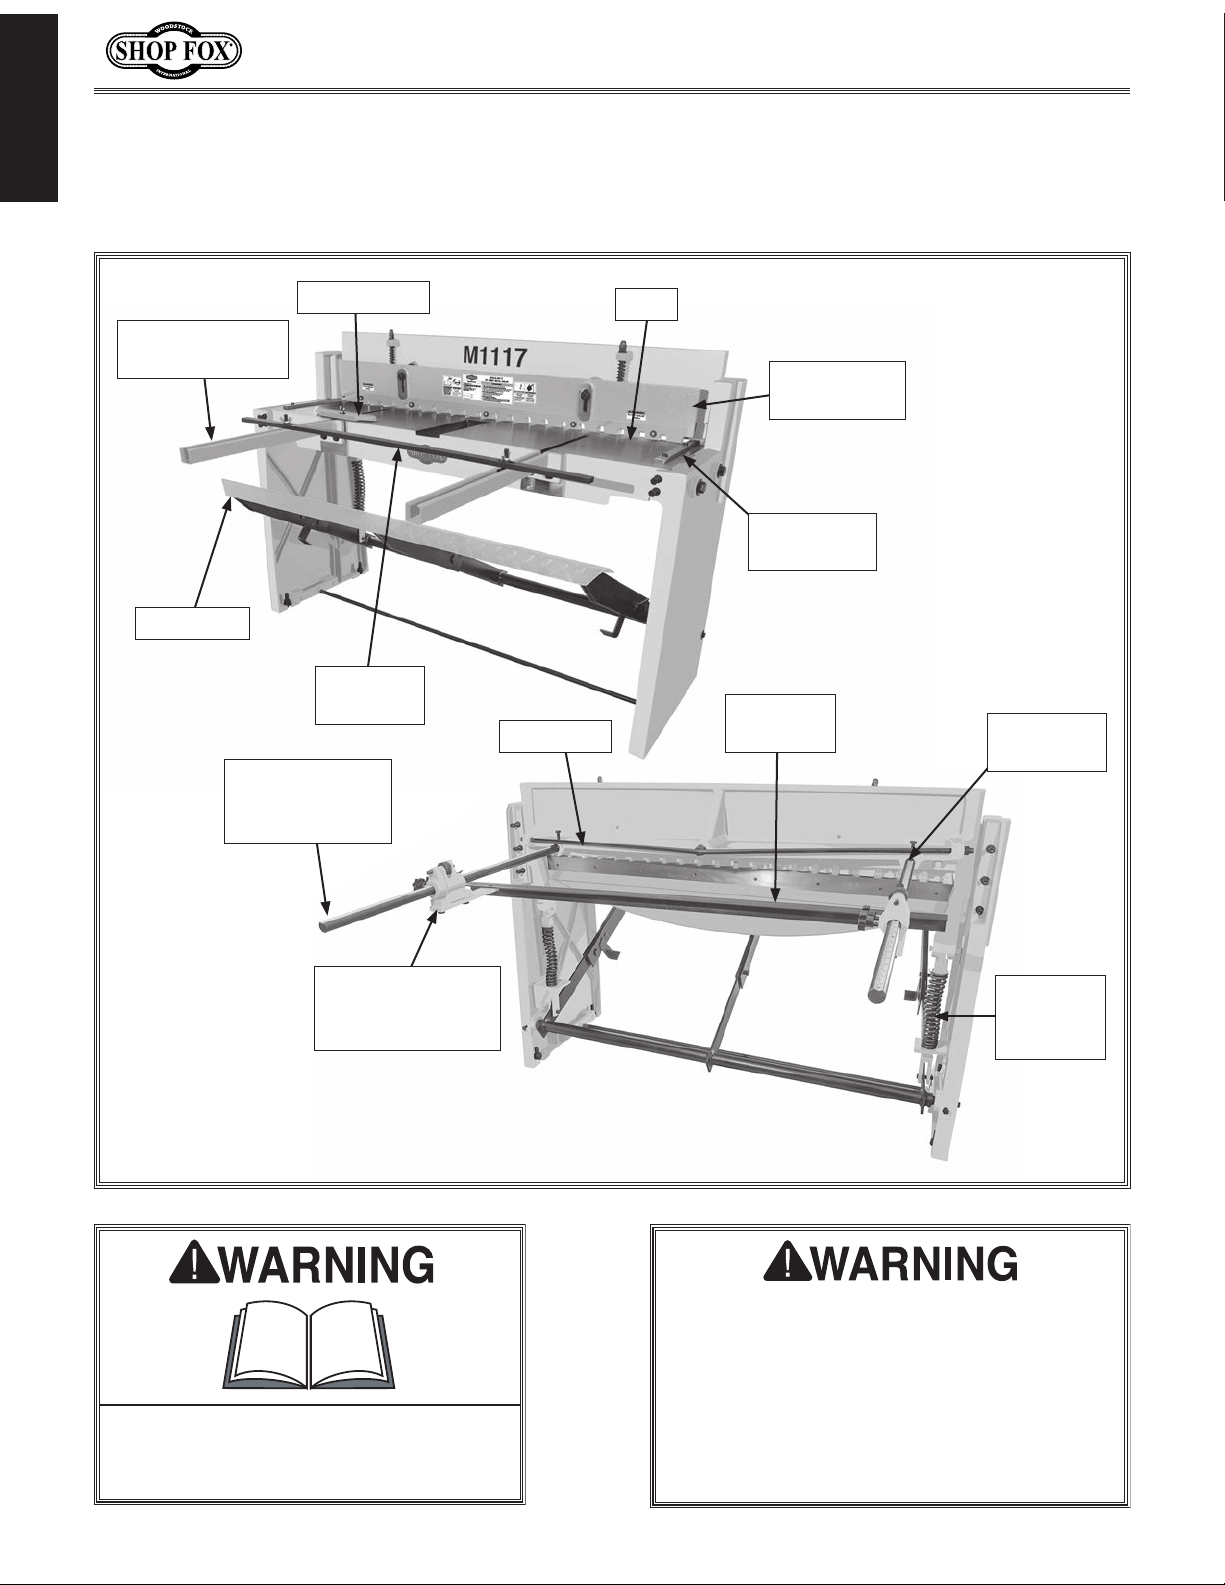
Become familiar with the names and locations of the controls and features shown below to better
Model M1117 (For Machines Mfd. Since 9/21)
Identification
Front Extension
Arm (1 of 2)
Foot Pedal
Rear Work Stop
Support Rod
Bevel Gauge
Front
Work Stop
(1 of 2)
Blade Bow
Table
Hold-Down/
Blade Guard
Front Scale
(1 of 2)
Rear
Work Stop
Rear Scale
(1 of 2)
Micro-Adjustable
Rear Work Stop
Assembly (1 of 2)
USE this and other machinery with caution
and respect. Always consider safety first,
as it applies to your individual working
conditions. No list of safety guidelines can
be complete—every shop environment is
To reduce your risk of serious injury
or damage to the machine, read this
entire manual BEFORE using machine.
-4-
different. Failure to follow guidelines could
result in serious personal injury, damage to
equipment or poor work results.
Extension
Spring
(1 of 2)
Page 7
Model M1117 (For Machines Mfd. Since 9/21)
Controls & Components
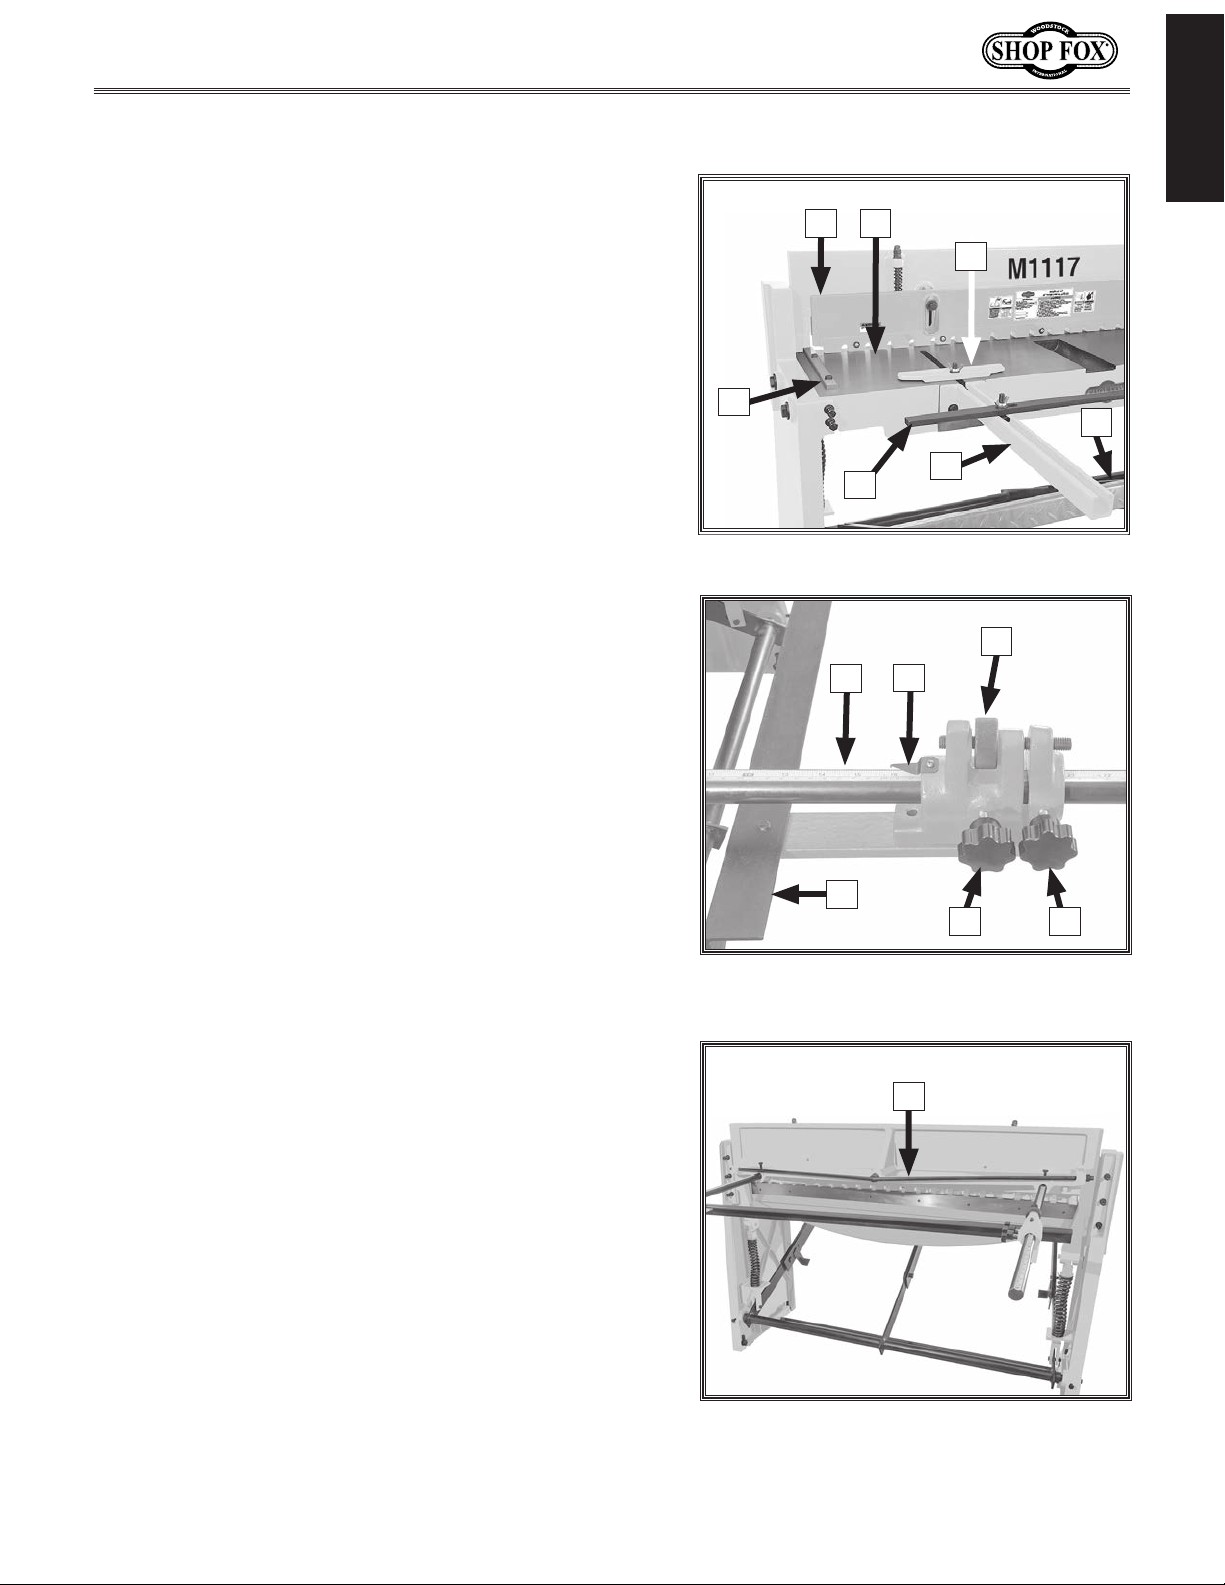
Refer to the Figures 1-3 and the following descriptions to
become familiar with the basic controls and components
of this machine. Understanding these items and how they
work will help you understand the rest of the manual and
stay safe when operating this machine.
A. Hold-Down/Blade Guard: Holds down workpiece and
protects user from blades during shearing operation.
INTRODUCTION
A
B
C
B. Table: Supports infeed side of workpiece.
C. Bevel Gauge: Secures front edge of angled
workpieces.
D. Foot Pedal: Controls cutting action of upper blade.
E. Front Extension Arm (1 of 2): Provides infeed
support for large workpieces and extends front work
stop and bevel track.
F. Front Work Stop: Adjusts on front extension arms
and holds workpiece in place during shearing
operation.
G. Front Scale (1 of 2): Indicates distance from cutting
line; keeps workpiece square with blades.
H. Rear Work Stop Support Rod (1 of 2): Supports
work stop and has scale for approximate positioning
0-33".
I. Rear Work Stop Indicator: Indicates rear work stop
position on scale.
G
D
F
Figure 1. Infeed components and controls.
H
M
Figure 2. Outfeed components and
controls.
E
J
I
KL
J. Micro-Adjustment Knob (1 of 2): Fine-tunes rear
work stop position.
K. Rear Work Stop Lock Knob (1 of 2): Loosen to
adjust rear work stop position; tighten to secure.
L. Micro-Adjustment Lock Knob (1 of 2): Loosen to
fine-tune rear work stop position; tighten to secure.
M. Rear Work Stop: Adjusts on rear work stop support
rods to measure workpieces for repeatable cuts.
N. Blade Bow: Adjusts to keep upper blade straight
along its length.
-5-
N
Figure 3. Location of blade bow rod.
Page 8
Model M1117 (For Machines Mfd. Since 9/21)
SAFETY
OWNER’S MANUAL.
TRAINED OPERATORS ONLY.
DANGEROUS ENVIRONMENTS.
MENTAL ALERTNESS REQUIRED.
electrical components or improperly grounded
manual uses a series of symbols and signal words intended to convey the level of importance of the
safety messages. The progression of symbols is described below. Remember that safety messages by
SAFETY
For Your Own Safety,
Read Manual Before Operating Machine
The purpose of safety symbols is to attract your attention to possible hazardous conditions. This
SAFETY
themselves do not eliminate danger and are not a substitute for proper accident prevention measures—this responsibility is ultimately up to the operator!
NOTICE
Standard Machinery Safety Instructions
Standard Machinery Safety Instructions
Indicates an imminently hazardous situation which, if not avoided,
WILL result in death or serious injury.
Indicates a potentially hazardous situation which, if not avoided,
COULD result in death or serious injury.
Indicates a potentially hazardous situation which, if not avoided,
MAY result in minor or moderate injury.
This symbol is used to alert the user to useful information about
proper operation of the equipment or a situation that may cause
damage to the machinery.
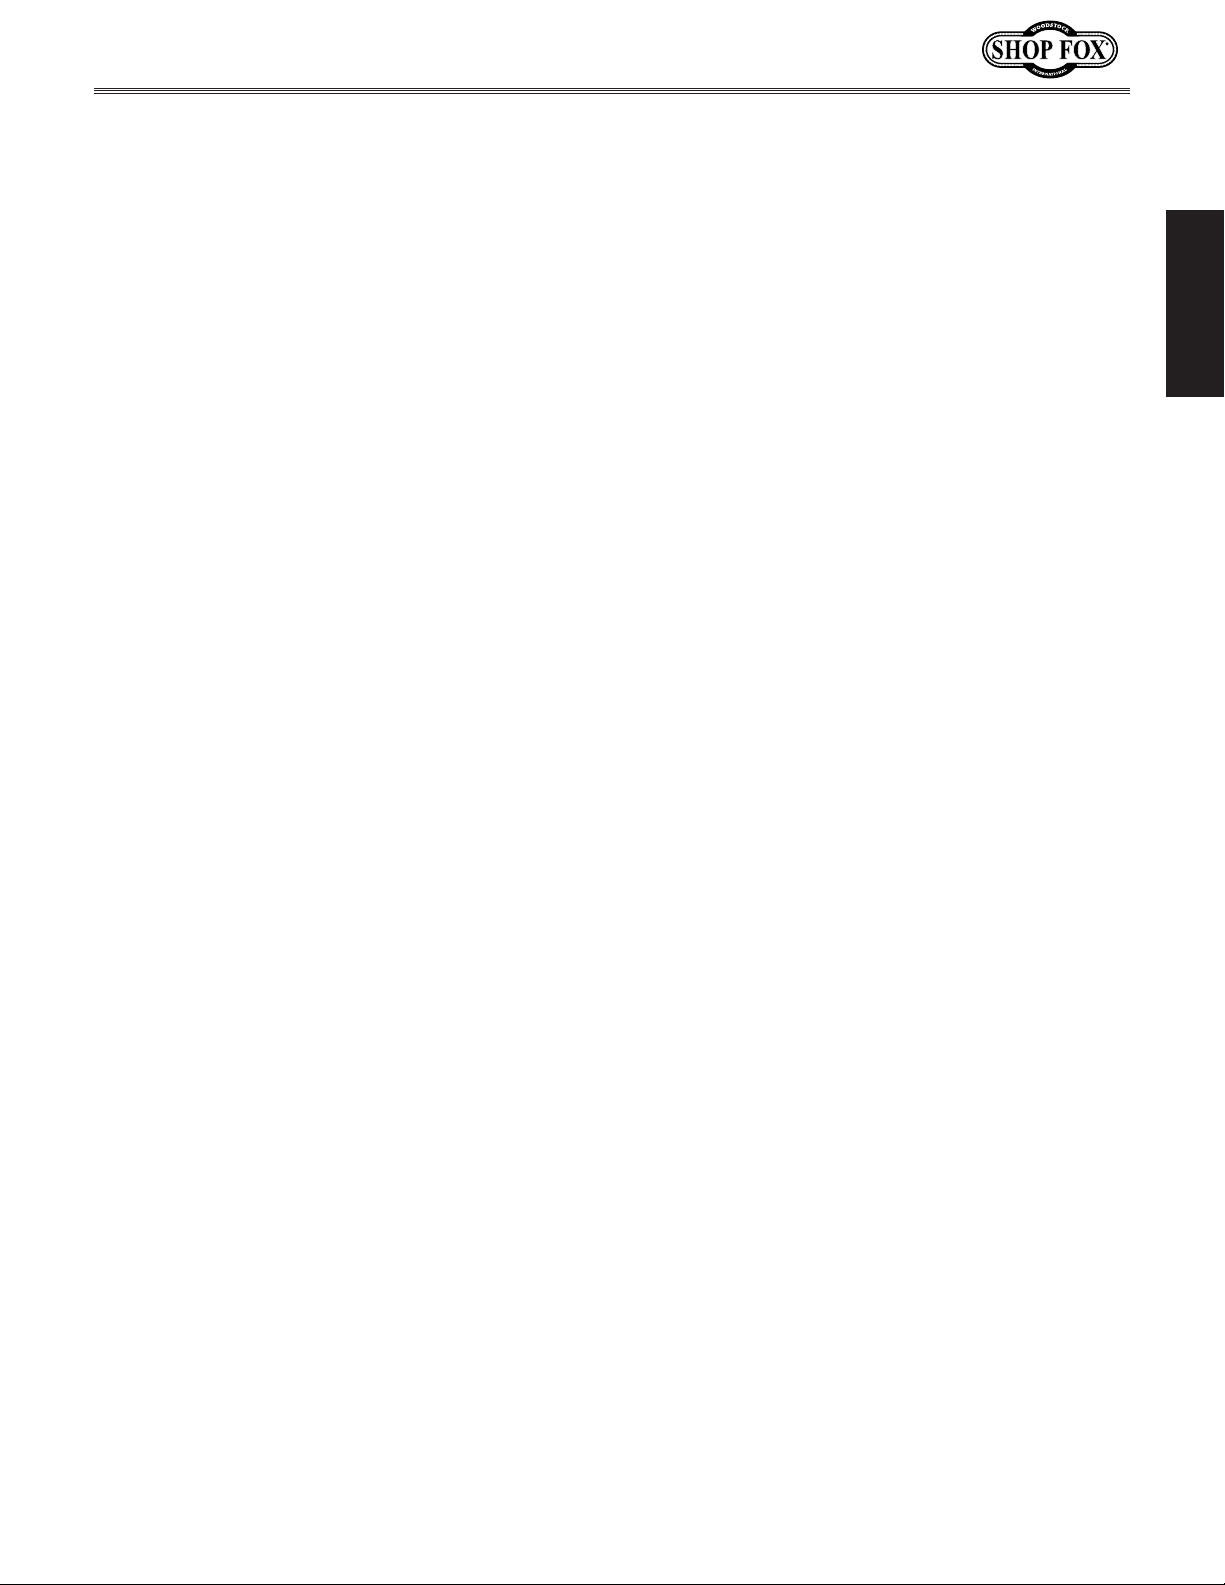
Read and understand this
owner’s manual BEFORE using machine.
have a higher risk of being hurt or killed. Only
allow trained/supervised people to use this
machine. When machine is not being used,
disconnect power, remove switch keys, or
lock-out machine to prevent unauthorized
use—especially around children. Make
workshop kid proof!
machinery in areas that are wet, cluttered,
or have poor lighting. Operating machinery
in these areas greatly increases the risk of
accidents and injury.
alertness is required for safe operation of
machinery. Never operate under the influence
of drugs or alcohol, when tired, or when
distracted.
Untrained operators
Do not use
Full mental
ELECTRICAL EQUIPMENT INJURY RISKS. You can
be shocked, burned, or killed by touching live
machinery. To reduce this risk, only allow an
electrician or qualified service personnel to
do electrical installation or repair work, and
always disconnect power before accessing or
exposing electrical equipment.
DISCONNECT POWER FIRST. Always disconnect
machine from power supply BEFORE making
adjustments, changing tooling, or servicing
machine. This eliminates the risk of injury
from unintended startup or contact with live
electrical components.
EYE PROTECTION. Always wear ANSI-approved
safety glasses or a face shield when operating
or observing machinery to reduce the risk of
eye injury or blindness from flying particles.
Everyday eyeglasses are not approved safety
glasses.
-6-
Page 9
Model M1117 (For Machines Mfd. Since 9/21)
WEARING PROPER APPAREL. Do not wear
HAZARDOUS
HEARING PROTECTION.
REMOVE ADJUSTING TOOLS.
INTENDED USAGE.
AWKWARD POSITIONS.
CHILDREN & BYSTANDERS.
GUARDS & COVERS.
FORCING MACHINERY. Do not force machine. It
will do the job safer and better at the rate for
loss of control. Before starting, verify machine
malfunction, leading to serious personal injury
from heated surfaces, high traffic areas, harsh
clothing, apparel, or jewelry that can become
entangled in moving parts. Always tie back
or cover long hair. Wear non-slip footwear to
avoid accidental slips, which could cause loss
of workpiece control.
DUST. Dust created while using
machinery may cause cancer, birth defects,
or long-term respiratory damage. Be aware of
dust hazards associated with each workpiece
material, and always wear a NIOSH-approved
respirator to reduce your risk.
Always wear hearing
protection when operating or observing
loud machinery. Extended exposure to this
noise without hearing protection can cause
permanent hearing loss.
machinery can become dangerous projectiles
upon startup. Never leave chuck keys,
wrenches, or any other tools on machine.
Always verify removal before starting!
intended purpose—never make modifications
without prior approval from Woodstock
International. Modifying machine or using
it differently than intended will void the
warranty and may result in malfunction or
mechanical failure that leads to serious
personal injury or death!
balance at all times when operating machine.
Do not overreach! Avoid awkward hand
positions that make workpiece control difficult
or increase the risk of accidental injury.
bystanders at a safe distance from the work
area. Stop using machine if they become a
distraction.
Only use machine for its
Tools left on
Keep proper footing and
Keep children and
which it was designed.
NEVER STAND ON MACHINE. Serious injury may
occur if machine is tipped or if the cutting
tool is unintentionally contacted.
STABLE MACHINE. Unexpected movement during
operation greatly increases risk of injury or
is stable and mobile base (if used) is locked.
USE RECOMMENDED ACCESSORIES. Consult
this owner’s manual or the manufacturer for
recommended accessories. Using improper
accessories will increase risk of serious injury.
UNATTENDED OPERATION. To reduce the risk
of accidental injury, turn machine OFF and
ensure all moving parts completely stop
before walking away. Never leave machine
running while unattended.
MAINTAIN WITH CARE. Follow all maintenance
instructions and lubrication schedules to
keep machine in good working condition. A
machine that is improperly maintained could
or death.
CHECK DAMAGED PARTS. Regularly inspect
machine for any condition that may affect
safe operation. Immediately repair or replace
damaged or mis-adjusted parts before
operating machine.
MAINTAIN POWER CORDS. When disconnecting
cord-connected machines from power, grab
and pull the plug—NOT the cord. Pulling the
cord may damage the wires inside, resulting
in a short. Do not handle cord/plug with wet
hands. Avoid cord damage by keeping it away
chemicals, and wet/damp locations.
SAFETY
accidental contact with moving parts or flying
debris—make sure they are properly installed,
undamaged, and working correctly.
Guards and covers reduce
EXPERIENCING DIFFICULTIES. If at any time
you experience difficulties performing the
intended operation, stop using the machine!
-7-
Contact Technical Support at (360) 734-3482.
Page 10
Model M1117 (For Machines Mfd. Since 9/21)
FINGER AMPUTATION.
CAPACIT Y.
BLADE CONDITION.
SHEAR BLADE ADJUSTMENT.
PROPER WORKPIECE MATERIAL.
WORK AREA
hand positions where a sudden slip could cause
before performing any adjustments, service, or
Before using machine, carefully
play, and ensure guards are properly installed.
Sheet metal cut-off
cut-off sheet metal pieces from the floor after
Serious cuts, amputation, or death can occur from contact with shear blades during operation,
Additional Safety for Metal Shears
adjustment, or maintenance. To reduce this risk, anyone using this machine MUST completely
heed the hazards and warnings below.
down can easily pinch, crush, or amputate
SAFETY
fingers or other body parts. Always keep
hands, fingers, and other body parts away
from blades and hold-down (point-of-operation)
during shearing operations.
Exceeding cutting capacity of shear
may result in breakage or machine damage
that ejects dangerous metal debris at operator
or bystanders. Only use sheet metal within
the rated capacity of this shear (refer to the
Machine Specifications).
properly adjusted blades will reduce risk
of injury from breakage or sharp burrs left
on workpiece. Always keep blades properly
adjusted and sharp.
or replacing shear blades, always wear heavy
leather gloves to protect hands and wear safety
glasses to protect eyes.
intended for cutting ferrous and non-ferrous
mild sheet metal or flat stock. Do not attempt
to cut round metal stock, glass, wood, drywall,
backer board, plywood, or other material not
intended for this machine. Cutting incorrect
materials can produce unexpected results,
which increases risk of injury, and may result
in damage to machine.
. Provide sufficient clearance
around machine to permit safe use by regular
operators and performance of maintenance
procedures. Keep work area clear of materials
or substances that may create a slip, trip, or
fall hazard.
The shear blades or hold-
Sharp, undamaged, and
When adjusting
Shear is only
SHARP METAL EDGES. The sharp metal edges of
sheet metal can easily cut fingers, hands, and
other body parts. Always wear heavy leather
gloves when handling sheet metal. Always
chamfer and deburr sharp metal workpiece
edges.
OPERATOR POSITION. Avoid awkward body and
your hand or body to enter point-of-operation
or make accidental contact with shear blades.
MAINTENANCE/SERVICE. Always wait for all
moving parts to come to a complete stop
maintenance. Do not contact foot pedal while
performing these adjustments.
GUARDS. Keep all guards in place, properly
positioned, and in working order. Never
operate shear with blade guard removed.
If blade guard is removed or not properly
positioned, fingers may accidentally be cut or
amputated by shear blades. Always position
guard just high enough to allow workpiece to
enter, but not high enough for fingers.
CHECK MACHINE.
check components for wear that could affect
operation. Check blade alignment and gib
DO NOT operate machine until all defects are
corrected.
STRAY SHEET METAL PIECES.
pieces left on the floor can easily slide under
foot and cause falling injuries. Always remove
operation. Keep work area clean.
-8-
Page 11
Model M1117 (For Machines Mfd. Since 9/21)
This machine has been carefully packaged for safe
transportation. If you notice the machine has been
damaged during shipping, please contact your authorized
Shop Fox dealer immediately.
The following items are needed, but not included, to set
up your machine.
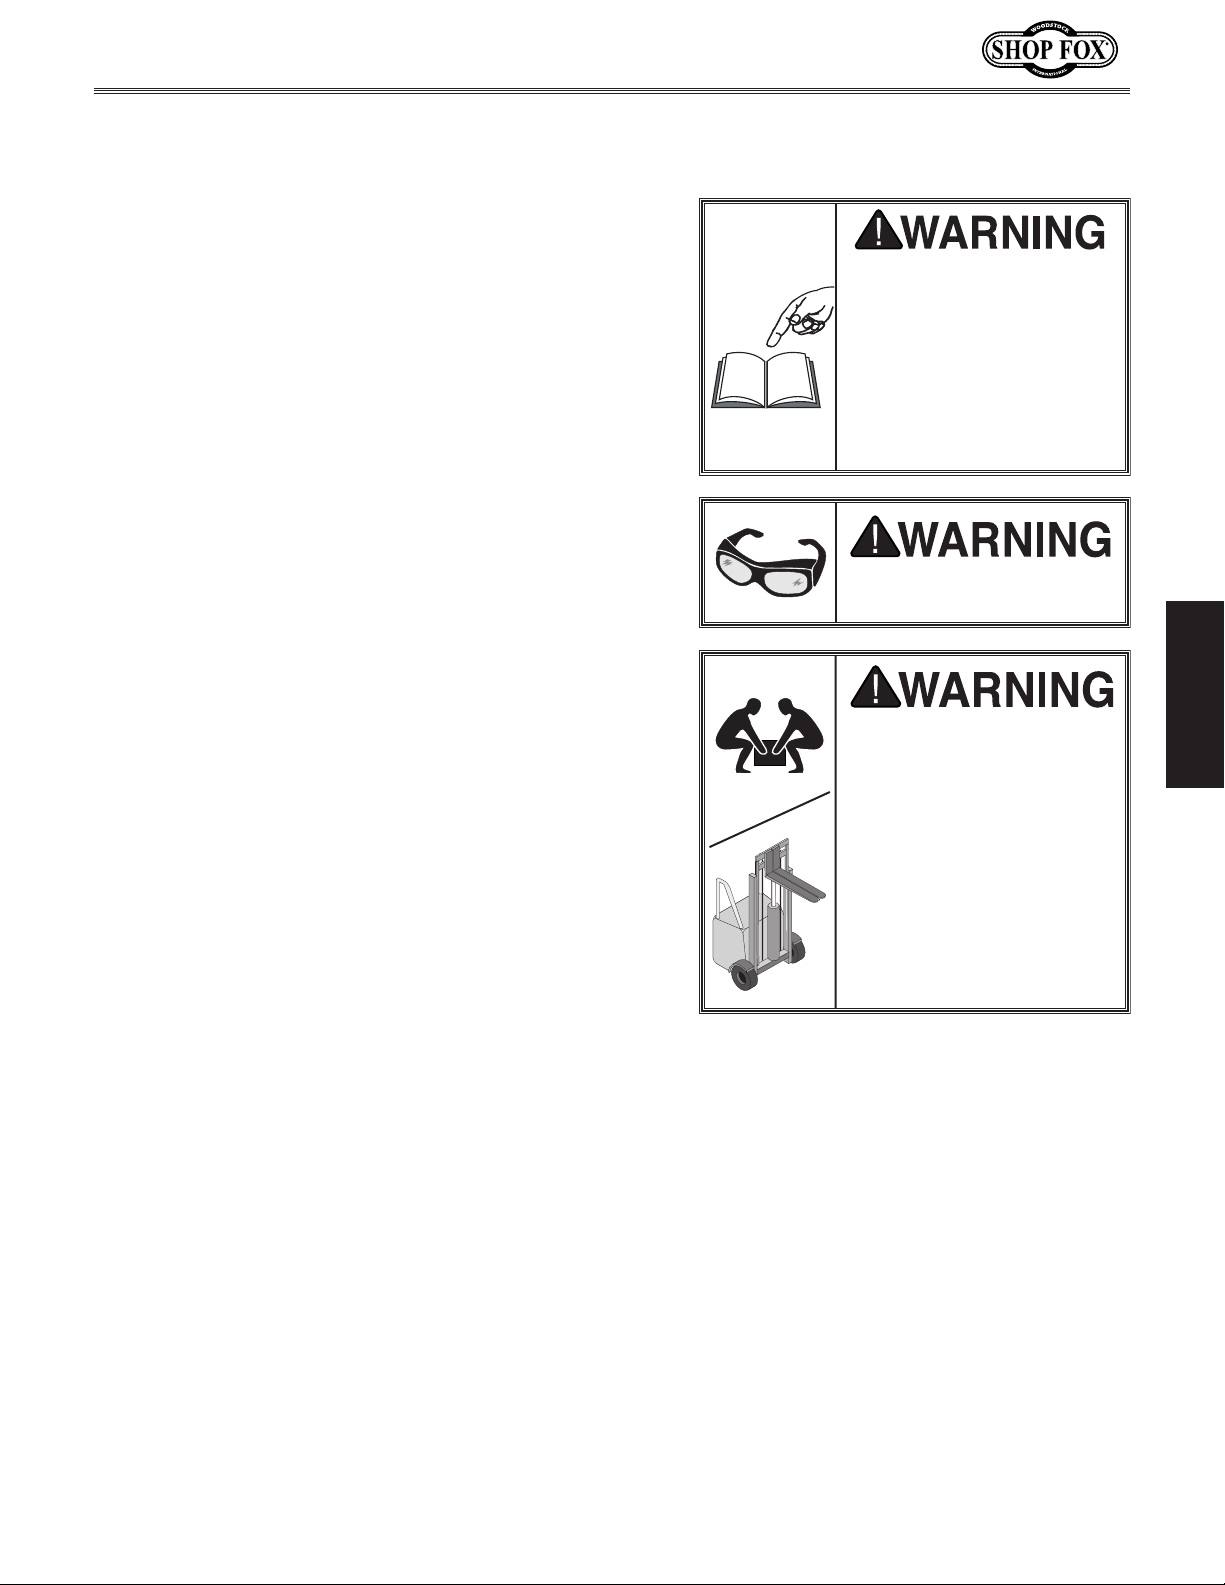
This machine presents
serious injury hazards
to untrained users. Read
to become familiar with
tions before starting the
Straining or crushing
improperly lifting the
parts. To reduce this
SETUP
Unpacking
through this entire manual
the controls and opera-
Items Needed for Setup
Description Qty
• Safety Glasses for Each Person ......................1 Pr.
• Disposable Rags ................................ As Needed
• Disposable Gloves ............................. As Needed
• Cleaner/Degreaser ............................ As Needed
• Lifting Equipment (Rated for 1500 lbs.) ...............1
• Another Person .............................................1
• Floor Mounting Hardware .................... As Needed
• Precision Level .............................................1
• Wrench or Socket 10, 12mm ........................1 Ea.
• Tape Measure ...............................................1
machine!
Wear safety glasses during
entire setup process!
SETUP
HEAVY LIFT!
injury may occur from
machine or some of its
risk, get help from other
people and use a forklift
(or other lifting equipment) rated for weight of
machine.
-9-
Page 12
Model M1117 (For Machines Mfd. Since 9/21)
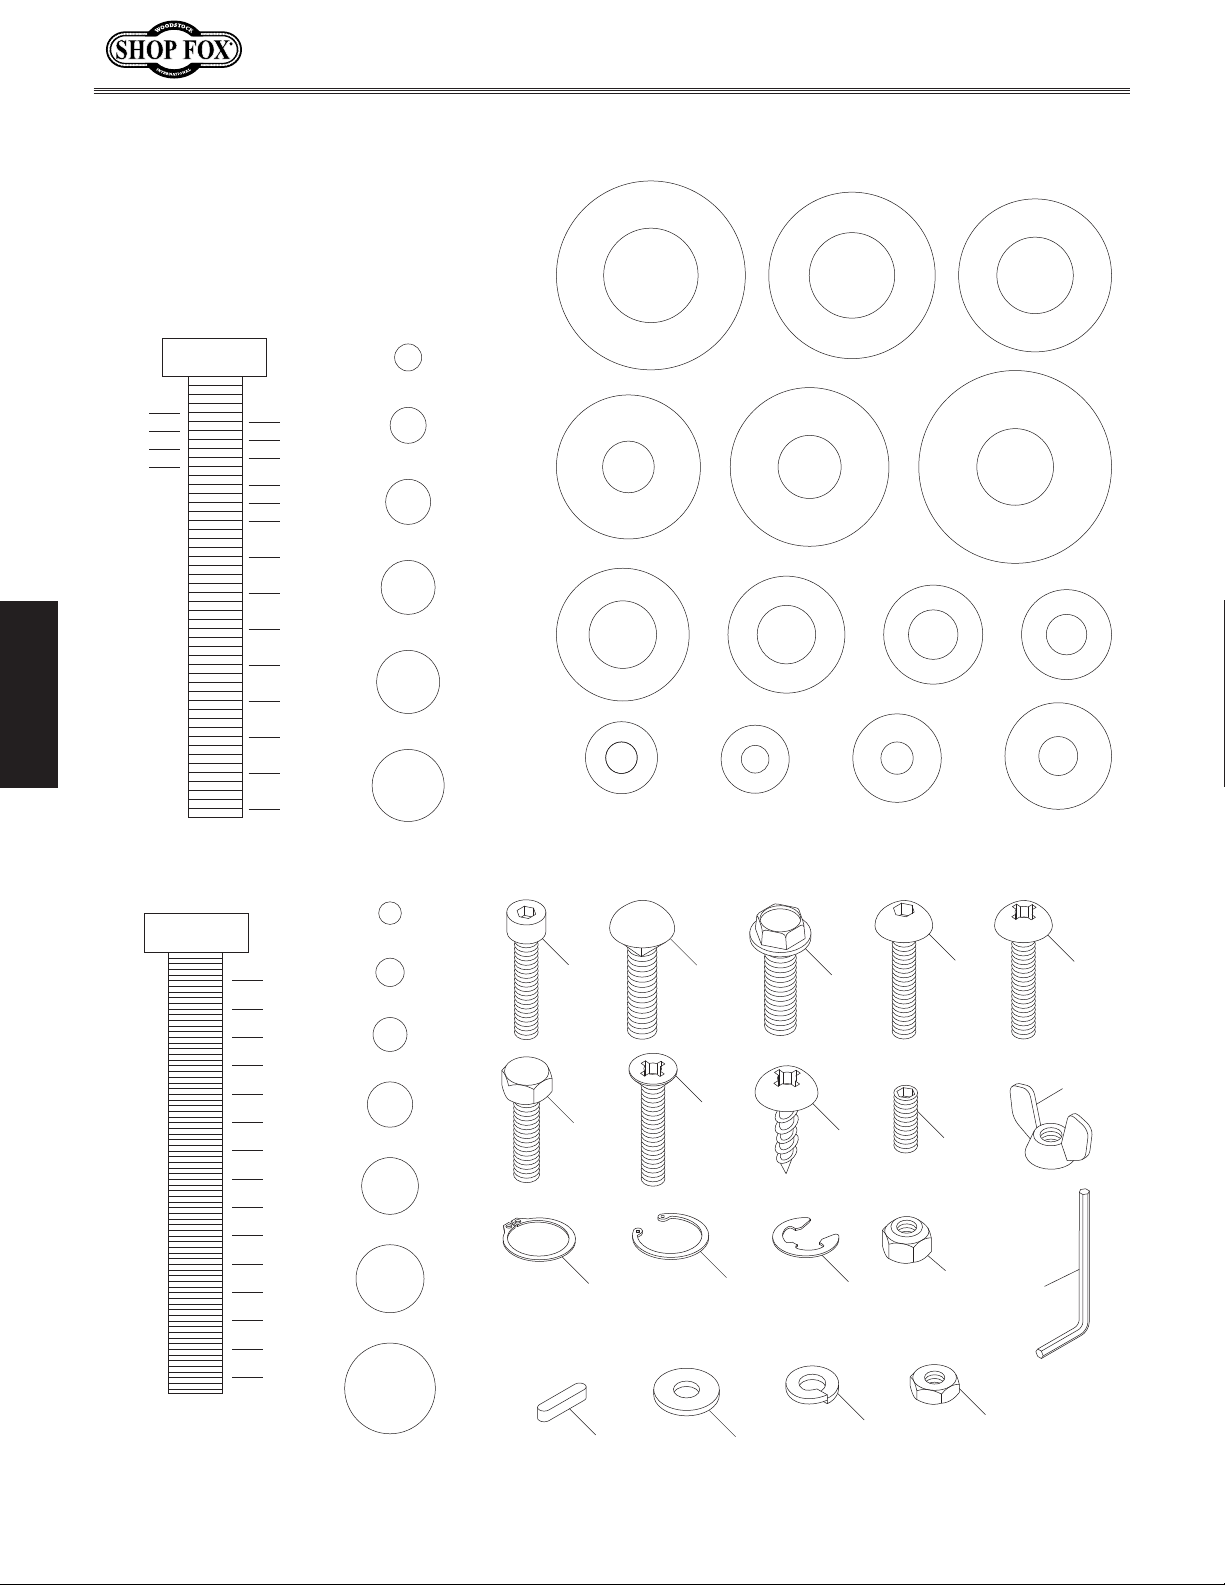
Hardware Recognition Chart
USE THIS CHART TO IDENTIFY
HARDWARE DURING THE
INVENTORY/ASSEMBLY
PROCESS.
1
⁄4"
3
⁄8"
1
⁄2"
5
⁄8"
⁄16" INCH APART
1
SETUP
LINES ARE
5
⁄16"
7
⁄16"
9
⁄16"
3
⁄4"
7
⁄8"
1
1
1
1
1
3
1
2
1
2
1
2
3
2
3
⁄4"
⁄2"
⁄4"
⁄4"
⁄2"
⁄4"
#10
1
⁄4"
5
⁄16"
3
⁄8"
7
⁄16"
1
⁄2"
D
I
A
R
E
H
S
A
W
R
E
H
8mm
S
A
W
R
E
H
S
7
A
⁄16"
W
D
R
E
H
S
A
W
WASHERS ARE MEASURED BY THE INSIDE DIAMETER
#10
M
E
T
E
5
⁄8"
D
I
A
D
I
A
I
A
M
E
T
E
R
R
M
E
T
E
R
M
E
T
E
R
E
H
S
A
D
R
E
H
S
A
W
4mm
R
E
H
S
10mm
A
W
D
R
3
⁄8"
W
I
A
M
E
T
E
R
D
I
A
R
A
E
T
9
⁄16"
M
E
T
E
R
M
E
T
E
R
H
S
A
A
I
D
M
R
E
E
H
S
D
I
R
E
H
S
A
W
5
A
A
M
E
R
⁄16"
W
E
T
T
E
R
E
H
S
A
W
D
I
I
A
M
E
R
5mm
E
H
S
A
W
R
E
12mm
W
D
R
1
D
⁄2"
I
A
E
H
S
R
E
H
S
A
6mm
I
M
R
A
A
E
1
⁄4"
W
D
W
M
E
T
E
R
T
E
R
D
I
A
M
E
T
E
R
I
A
M
E
T
E
R
5mm
10mm
15mm
20mm
25mm
30mm
35mm
MEASURE BOLT DIAMETER BY PLACING INSIDE CIRCLE
40mm
45mm
50mm
55mm
LINES ARE 1MM APART
60mm
65mm
70mm
75mm
4mm
5mm
6mm
8mm
10mm
12mm
16mm
Cap
Screw
Hex
Bolt
External
Retaining
Ring
Key
Carriage
Bolt
Flat
Head
Screw
Internal
Retaining
Ring
Flat Washer
Flange
Bolt
Tap
Screw
E-Clip
Lock
Washer
Button
Head
Screw
Set
Screw
Lock
Nut
Hex
Nut
Phillips
Head
Screw
Wing
Nut
Hex
Wrench
-10-
Page 13
Model M1117 (For Machines Mfd. Since 9/21)
Inventory
The following is a list of items shipped with your machine.
Before beginning setup, lay these items out and inventory
them.
Note: If you cannot find an item on this list, carefully
check around/inside the machine and packaging materials.
Often, these items get lost in packaging materials while
unpacking or they are pre-installed at the factory.
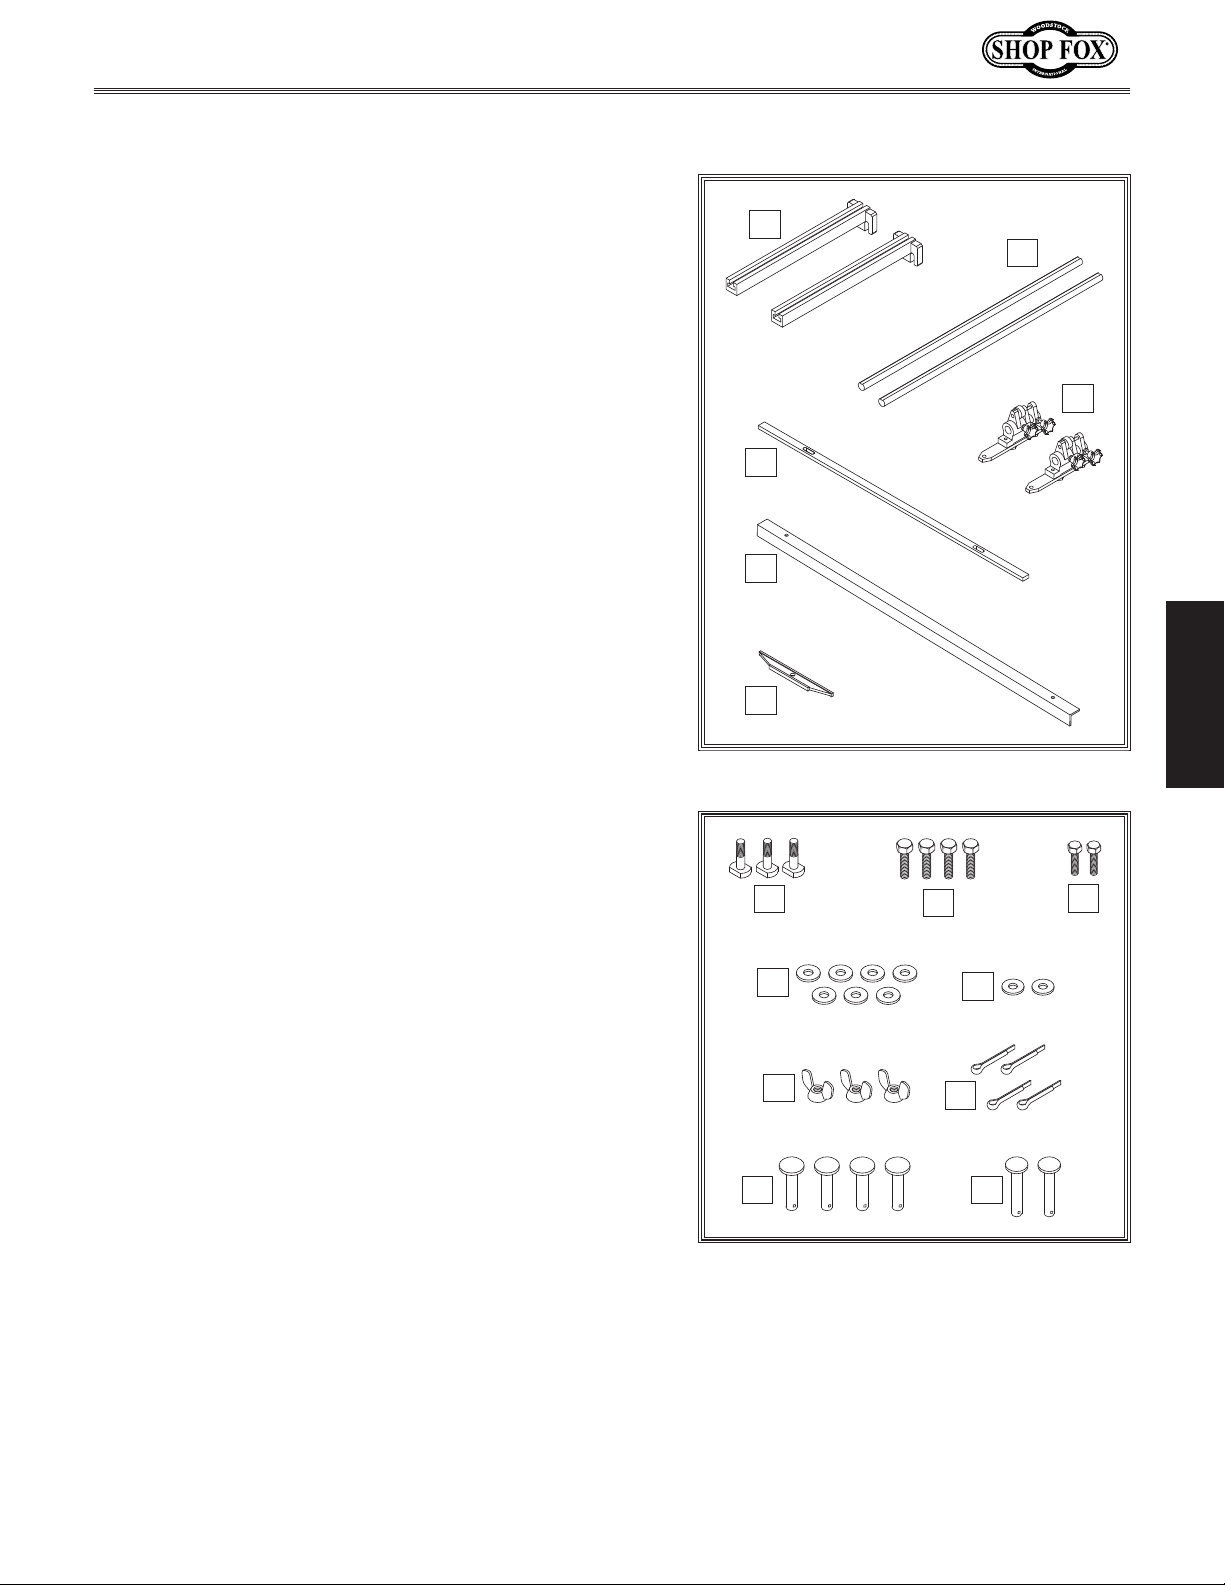
Loose Inventory (Figure 4): Qty
A. Front Extension Arms .....................................2
B. Rear Work Stop Support Rods ............................2
Front Work Stop ...........................................1
C.
D. Rear Work Stop Assemblies ..............................2
E. Rear Work Stop ............................................1
Bevel Gauge ................................................1
F.
A
B
D
C
E
Fasteners (Figure 5): Qty
G. T-Bolts M12-1.75 x 45 .....................................3
Hex Bolts M12-1.75 x 30 ..................................4
H.
I. Hex Bolts M10-1.5 x 20 ...................................2
J. Flat Washers 12mm .......................................7
K. Flat Washers 10mm .......................................2
L. Wing Nuts M12-1.75 .......................................3
Cotter Pins M3 x 50 .......................................4
M.
Clevis Pins 12 x 45mm ....................................4
N.
Clevis Pins 12 x 88mm ....................................2
O.
F
Figure 4. Loose inventory.
G
J
L
N
H
M
SETUP
I
K
O
-11-
Figure 5. Fasteners.
Page 14
To prevent
machine, the factory has coated t
of your machine
compound
I
be difficult to
coating is as easy as possible, please gather the correct
cleaner, lubricant, and tools listed below:
• Cleaner/degreaser
and grease
• Safety glasses & disposable gloves
•
• Disposable Rags
To
1.
2.
3
4
5
6
immediately coat with a quality metal protectant.
Cleaning Machine
corrosion during shipment and storage of your
with a heavy-duty rust prevention
.
f you are unprepared or impatient, this compound can
remove. To ensure that the removal of this
designed to remove storage wax
Solvent brush or paint brush
remove rust preventative coating, do these steps:
DISCONNECT MACHINE FROM POWER!
Model M1117 (For Machines Mfd. Since 9/21)
he bare metal surfaces
Gasoline and petroleum
products have low flash
points and can explode
or cause fire if used to
clean machinery. Avoid
using these products
to clean machinery.
Many cleaning solvents
are toxic if inhaled.
Minimize your risk
by only using these
products in a well
ventilated area.
SETUP
Put on safety glasses and disposable gloves.
. Coat the rust preventative with a liberal amount of
cleaner/degreaser, then let it soak for 5–10 minutes.
. Wipe off surfaces. If your cleaner/degreaser is
effective, the coating will wipe off easily.
Tip: An easier way to clean off thick coats of rust
preventative from flat surfaces is to use a PLASTIC
paint scraper to scrape off the majority of the
coating before wiping it off with your rag. (Do
not use a metal scraper or you may scratch your
machine.)
. Repeat cleaning steps as necessary until all of the
compound is removed.
. To prevent rust on freshly cleaned surfaces,
In a pinch, automotive degreasers,
mineral spirits or WD•40 can be used
to remove rust preventative coating.
Before using these products, though,
test them on an inconspicuous area of
your paint to make sure they will not
damage it.
-12-
Page 15
Model M1117 (For Machines Mfd. Since 9/21)
Physical Environment
The physical environment where the machine
is operated is important for safe operation
and longevity of components. For best results,
operate this machine in a dry environment
that is free from excessive moisture, hazardous
chemicals, airborne abrasives, or extreme
conditions. Extreme conditions for this type
of machinery are generally those where the
ambient temperature range is outside 41°–104°F;
the relative humidity range is outside 20–95%
(non-condensing); or the environment is subject
to vibration, shocks, or bumps.
Space Allocation
Consider the largest size of workpiece that
will be processed through this machine and
provide enough space around the machine
for adequate operator material handling or
the installation of auxiliary equipment. With
permanent installations, leave enough space
around the machine to open or remove doors/
covers as required by the maintenance and
service described in this manual.
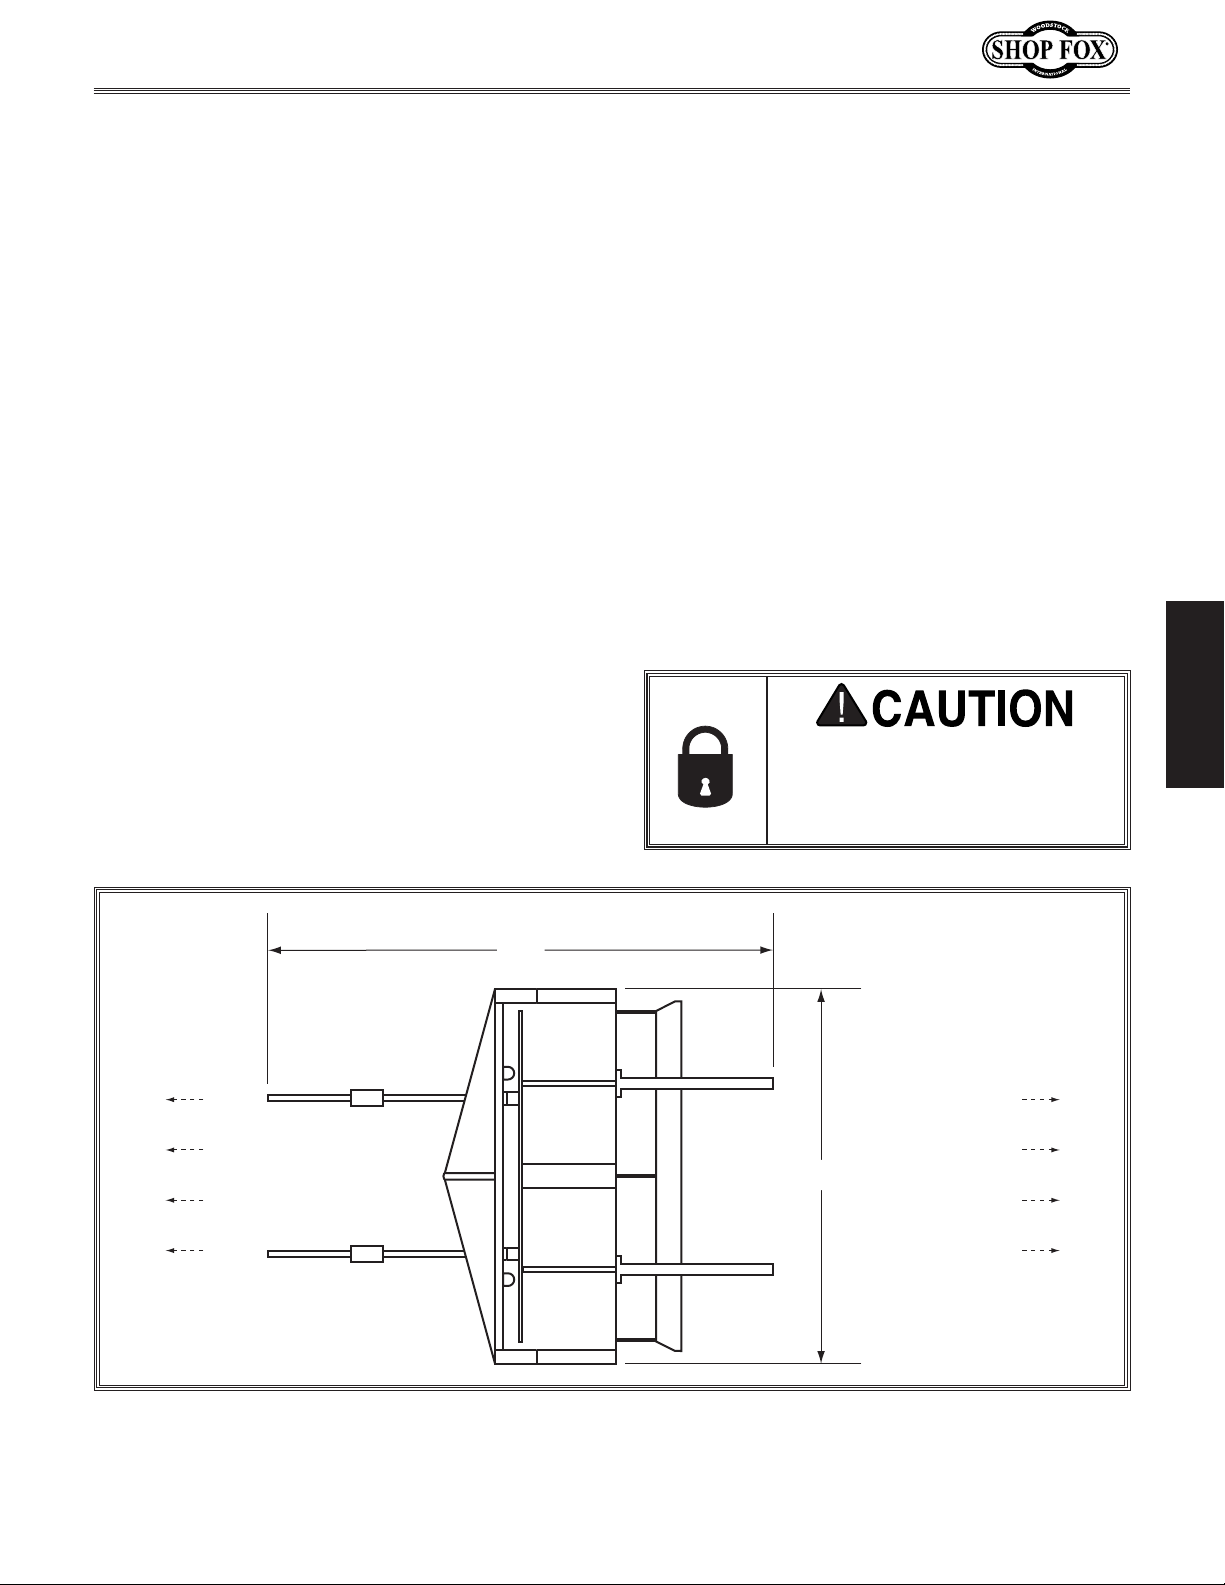
required space allocation.
Weight Load
machine. Only install in an access
Machine Placement
Refer to the Machine Specifications for the
weight of your machine. Make sure that the
surface upon which the machine is placed will
bear the weight of the machine, additional
equipment that may be installed on the
machine, and the heaviest workpiece that will
be used. Additionally, consider the weight of
the operator and any dynamic loading that may
occur when operating the machine.
Lighting
Lighting around the machine must be adequate
enough that operations can be performed
safely. Shadows, glare, or strobe effects that
may distract or impede the operator must be
eliminated.
SETUP
See below for
Keep Area
Unobstructed
Figure 6. Minimum working clearances.
74"
-13-
Children or untrained people
may be seriously injured by this
restricted location.
62"
Keep Area
Unobstructed
Page 16
Lifting & Moving
Straining or crushing
improperly lifting the
parts. To reduce this
Use a forklift (or other type of lifting equipment) with
lifting straps to move the machine to your desired
location. All lifting equipment should be rated for at least
1500 pounds.
Model M1117 (For Machines Mfd. Since 9/21)
HEAVY LIFT!
To lift and move machine, do these steps:
1. Place shipping crate near installation location, then
remove crate top and sides and set small items
aside.
Unbolt machine from shipping pallet.
2.
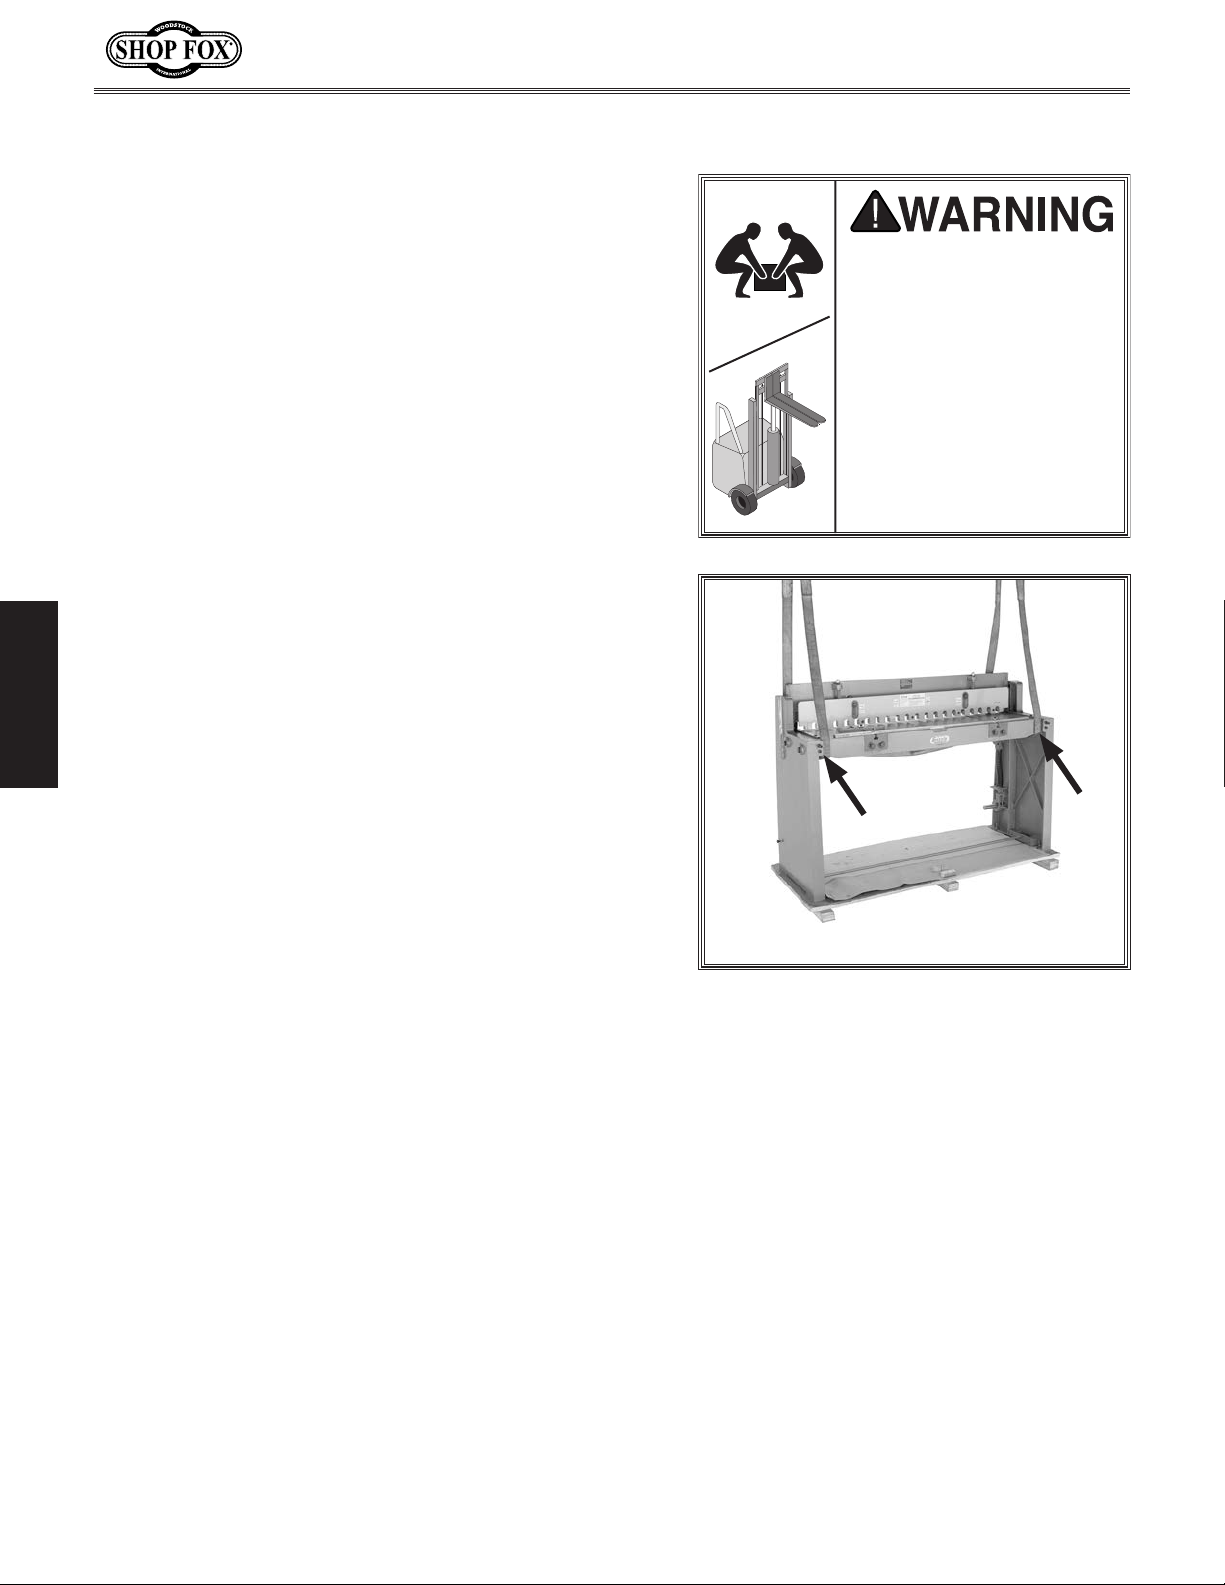
Place lifting straps under shear table at locations
3.
shown in Figure 7. Straps should be spread as wide
as possible.
With help of another person to steady load, use
4.
SETUP
forklift or crane to lift machine from pallet and
move to desired location.
injury may occur from
machine or some of its
risk, get help from other
people and use a forklift
(or other lifting equipment) rated for weight of
machine.
Figure 7. Example of lifting straps placed
under shear table for lifting.
-14-
Page 17
Model M1117 (For Machines Mfd. Since 9/21)
Anchoring machinery to the floor prevents tipping or
shifting and reduces vibration that may occur during
operation, resulting in a machine that runs slightly quieter
and feels more solid.
If the machine will be installed in a commercial or
workplace setting, or if it is permanently connected
(hardwired) to the power supply, local codes may require
that it be anchored to the floor.
If not required by any local codes, fastening the machine
to the floor is an optional step. If you choose not to do
this with your machine, we recommend placing it on
machine mounts, as these provide an easy method for
leveling and they have vibration-absorbing pads.
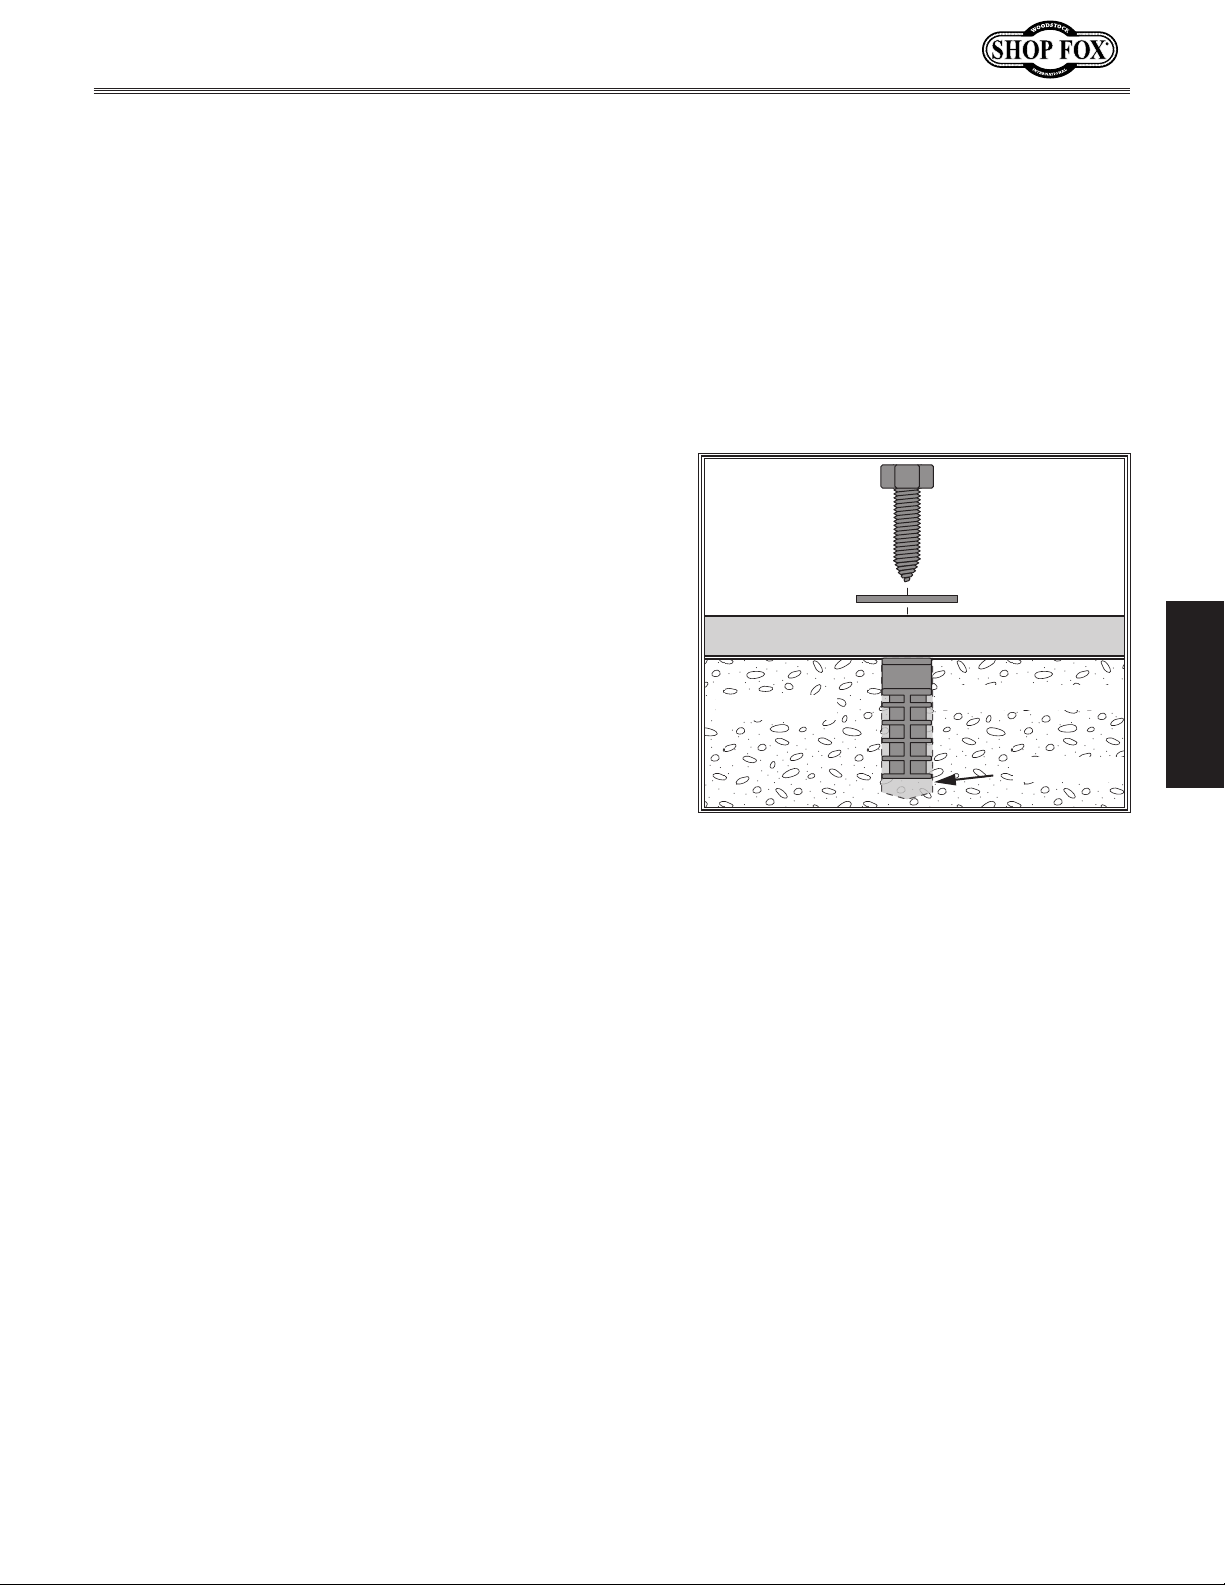
Lag shield anchors with lag screws (see Figure) are a
popular way to anchor machinery to a concrete floor,
because the anchors sit flush with the floor surface,
making it easy to unbolt and move the machine later, if
needed. However, anytime local codes apply, you MUST
follow the anchoring methodology specified by the code.
Anchoring to Floor
Number of Mounting Holes .................................. 4
Diameter of Mounting Hardware ........................5⁄8"
Lag Screw
Flat Washer
Anchoring to Concrete Floors
Machine Base
Lag Shield Anchor
Concrete
Drilled Hole
Figure 8. Popular method for anchoring
machinery to a concrete floor.
SETUP
-15-
Page 18
Assembly
Before beginning the assembly process, refer to Items
Needed for Setup
Ensure all parts have been properly cleaned of any
heavy-duty rust-preventative applied at the factory (if
applicable). Be sure to complete all steps in the assembly
procedure prior to performing the
or connecting
the machine to power.
and gather everything you need.
Test Run
To assemble machine, do these steps:
Model M1117 (For Machines Mfd. Since 9/21)
1. Use level to check shear table.
— If table is level, no adjustment is required. Proceed
to Step 2.
— If table is not level, use shims between floor and
base to level machine before proceeding. Leveling
shear helps blades and other components remain
straight and flat during life of machine so machine
can continue to cut straight and square.
SETUP
. Cut cable ties securing foot pedal to table.
2
. Have another person press and hold foot pedal about
3
halfway through full range of movement.
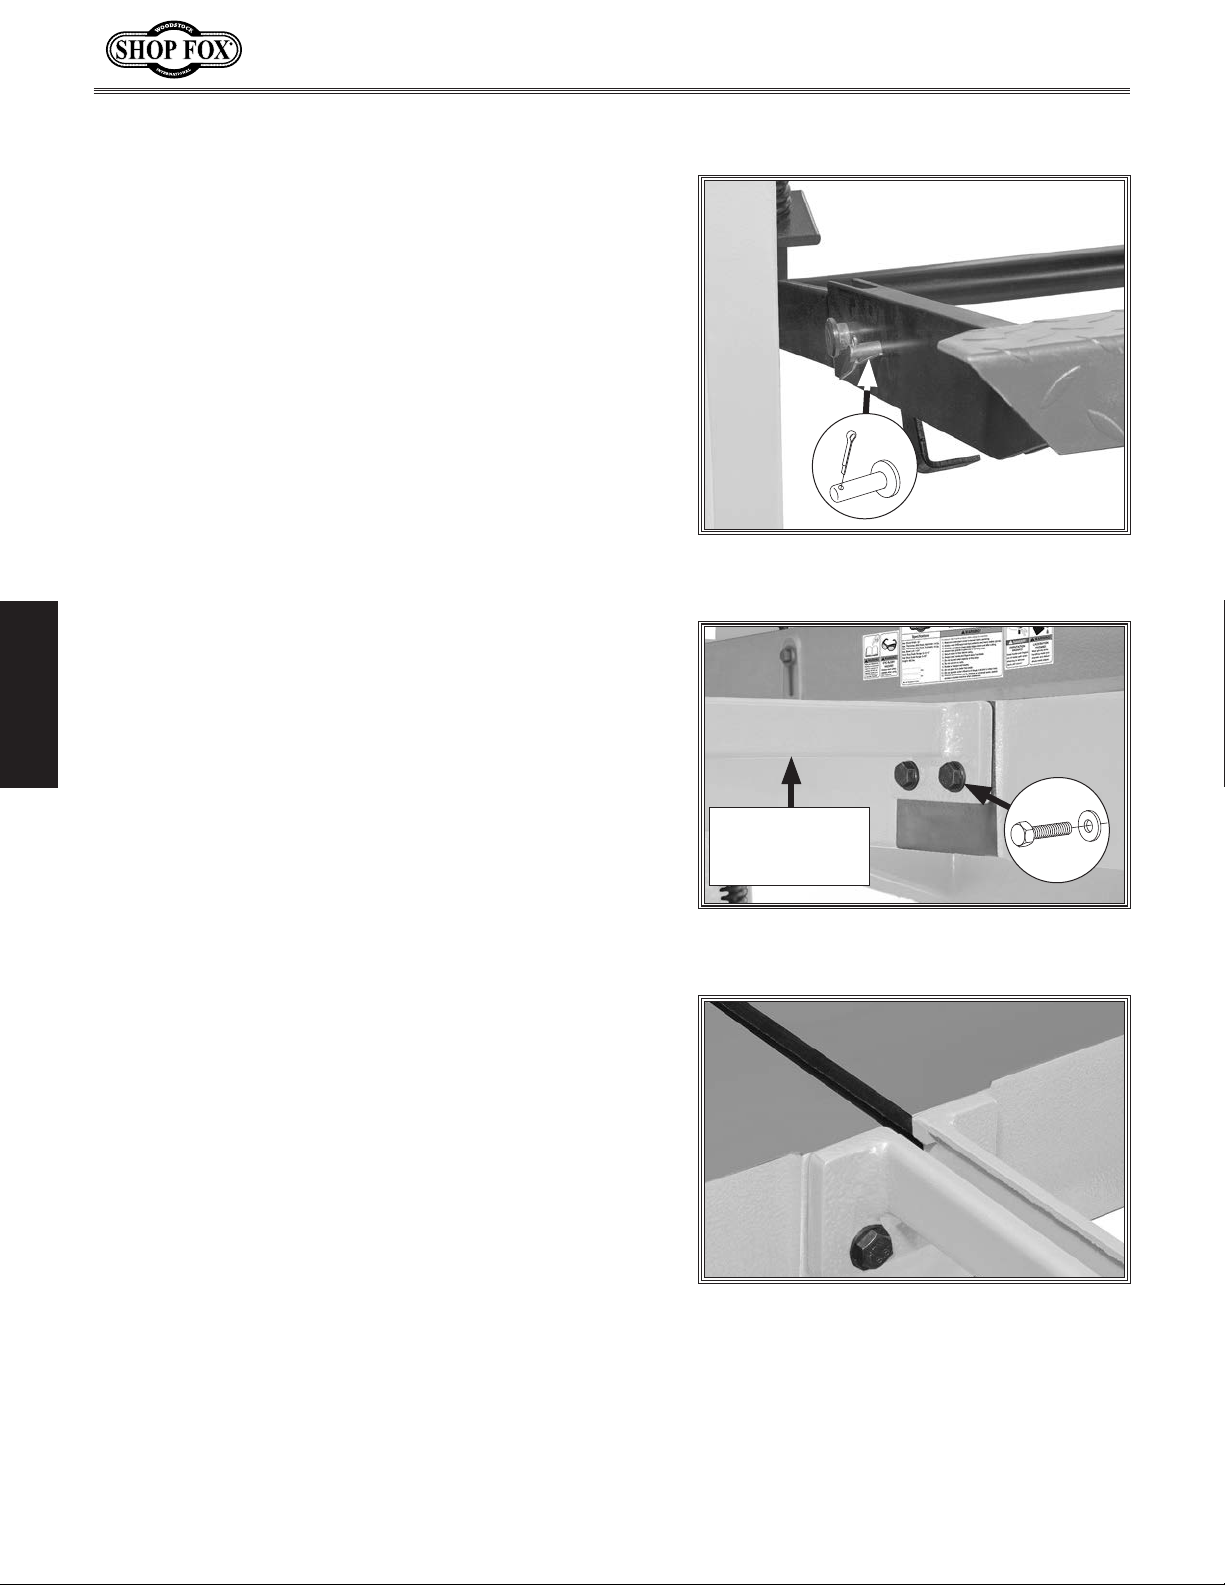
. Insert (2) 12 x 45mm clevis pins in holes in foot
4
pedal frame and secure with (2) M3 x 50 cotter pins,
as shown in Figure 9.
. Attach (2) front extension arms to shear table with
5
(4) M12-1.75 x 30 hex bolts and 12mm flat washers
(see Figure 10).
x 2
Figure 9. Location of hole in foot pedal
frame (1 of 2 shown).
Front
Extension Arm
(1 of 2)
Figure 10. Front extension arms attached
to shear table.
x 4
Note: Arm T-slots must line up with table T-slots,
and surfaces must be flush (see Figure 11).
Figure 11. Extension arm correctly
installed.
-16-
Page 19
Model M1117 (For Machines Mfd. Since 9/21)
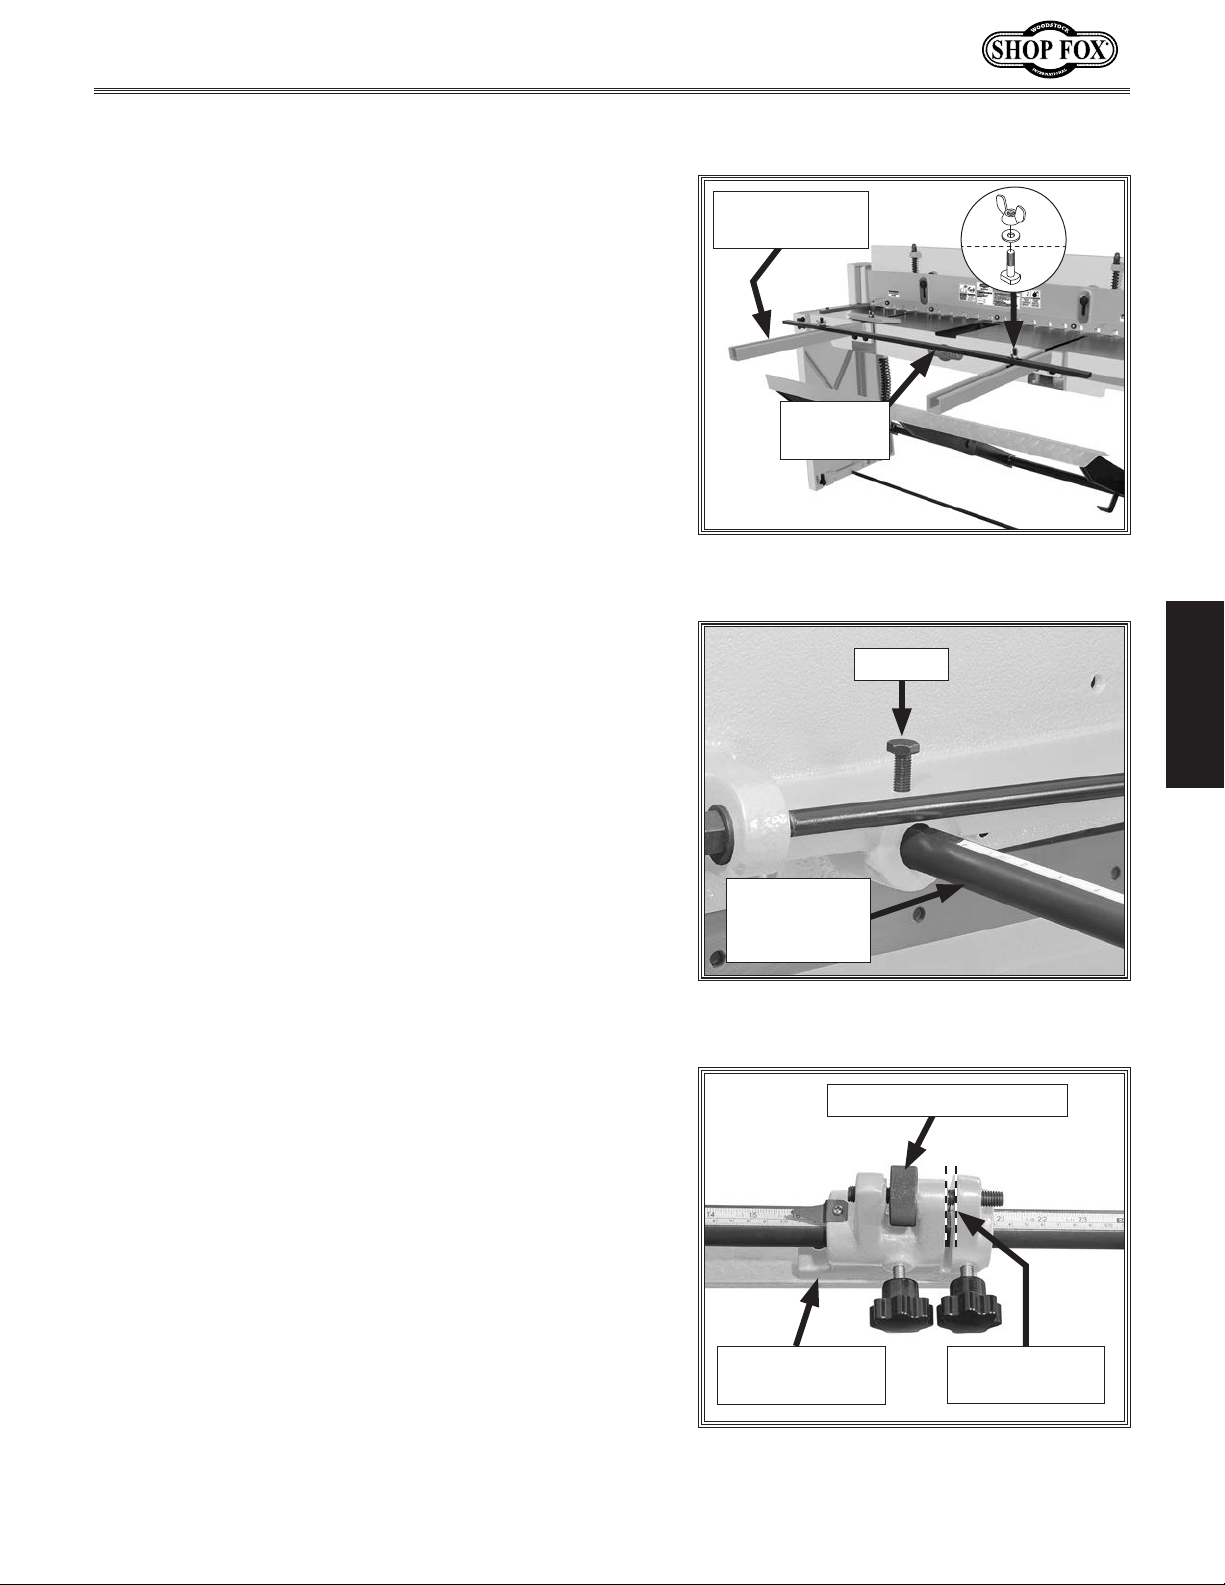
6. Install (1) M12-1.75 x 45 T-bolt in each T-slot and
secure front work stop to extension arms using (2)
12mm flat washers and M12-1.75 wing nuts (see
Figure 12).
7
. Insert (2) rear work stop support rods in holes shown
in Figure 13.
. Secure rear work stop support rods in place by
8
tightening pre-installed hex bolts (see Figure 13).
Extension Arm
(1 of 2)
x 2
Front
Work Stop
Figure 12. Front work stop secured to
extension arms.
Hex Bolt
SETUP
Note: Rear work stop support rods should extend
same distance from back of machine. If one rod
extends farther than the other, adjust hex bolts and
rods until even.
. Install (2) rear work stop assemblies onto rear work
9
stop support rods and tighten each micro-adjustment
knob completely to eliminate space shown
in Figure 14.
Rear Work
Stop Support
Rod (1 of 2)
Figure 13. Rear work stop support rod
installed on machine.
Micro-Adjustment Knob
Rear Work Stop
Assembly
Eliminate This
Space
-17-
Figure 14. Rear work stop assembly
installed on rear work stop support rod.
Page 20
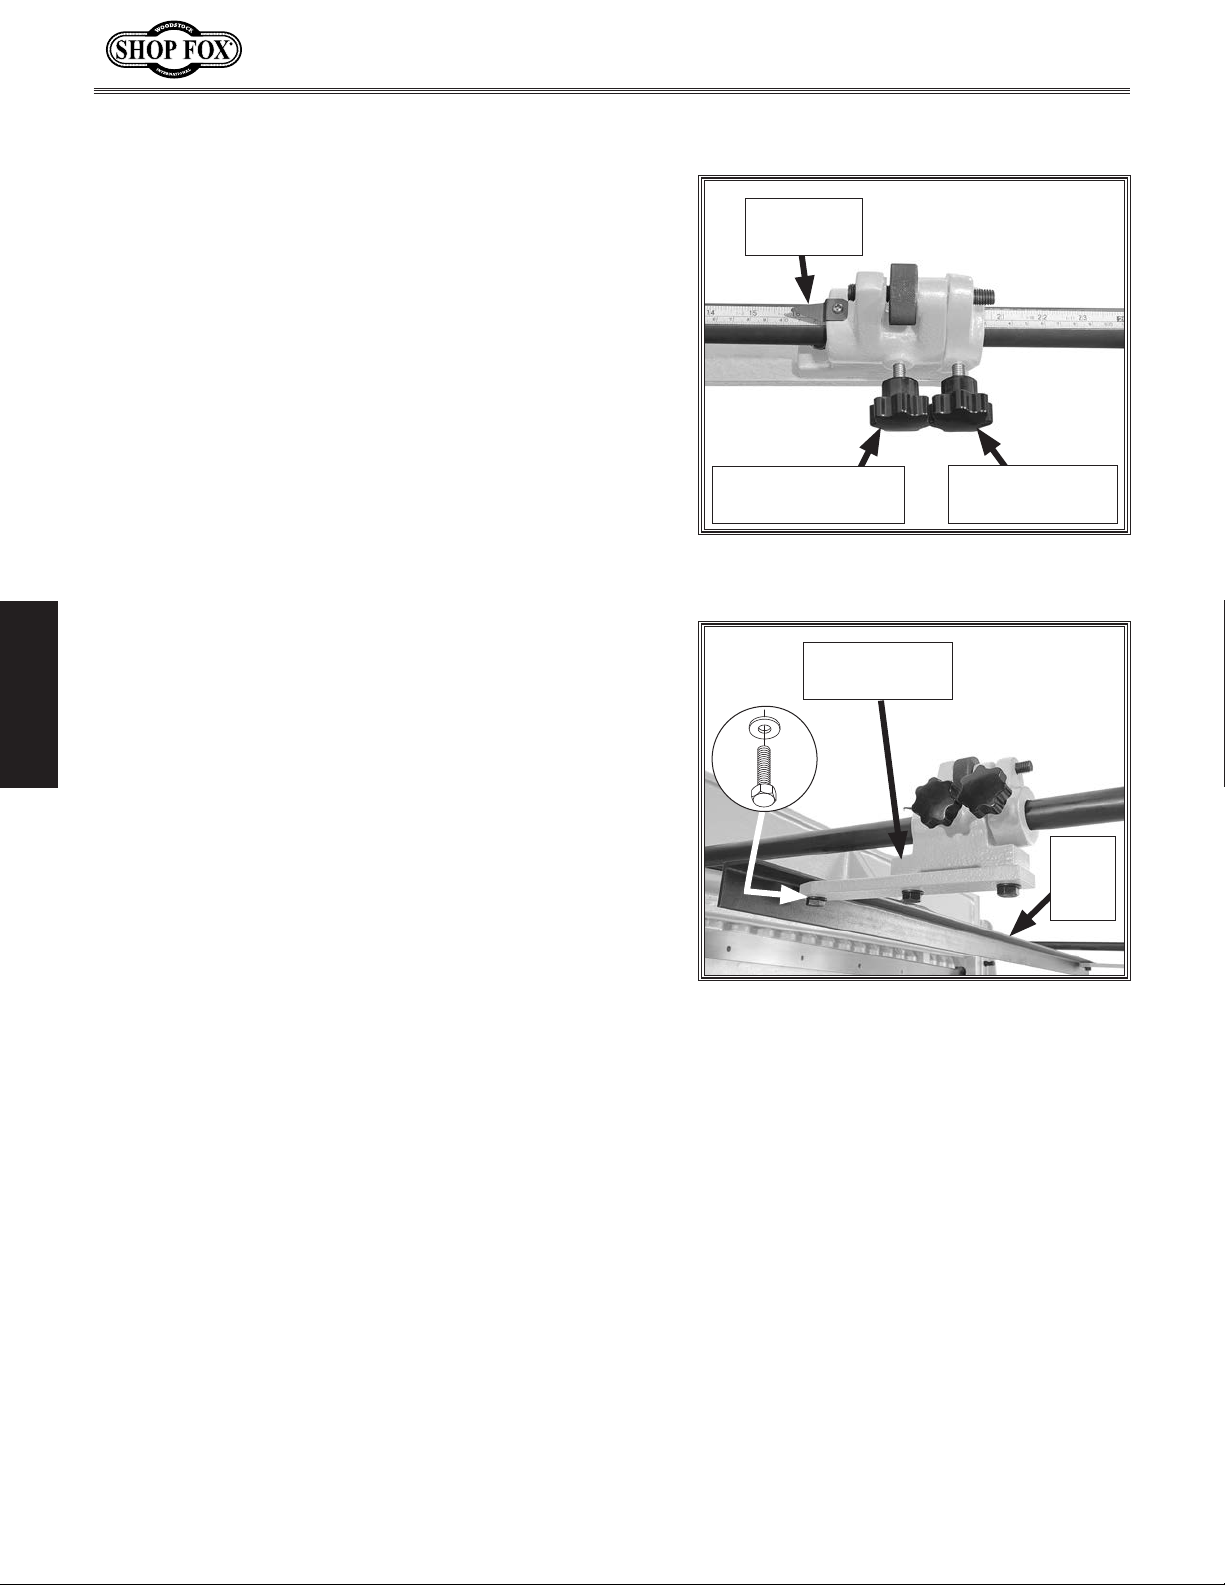
10. Align each work stop indicator to the same number
on rear work stop support rod scales, then tighten
micro-adjustment lock knobs and rear work stop lock
knobs (see Figure 15).
Model M1117 (For Machines Mfd. Since 9/21)
Work Stop
Indicator
Rear Work Stop
Lock Knob
11
. Attach rear work stop to rear work stop assemblies
with (2) M10-1.5 x 20 hex bolts and 10mm flat
washers, as shown in Figure 16.
Micro-Adjustment
Lock Knob
Figure 15. Rear work stop assembly
components.
Rear Work
Stop Assembly
SETUP
x 2
Rear
Work
Stop
Figure 16. Rear work stop attached to
rear work stop assembly.
-18-
Page 21
Model M1117 (For Machines Mfd. Since 9/21)
The purpose of this overview is to provide the novice
machine operator with a basic understanding of how
the machine is used during operation, so the
controls
easier to understand.
Due to the generic nature of this overview, it is
intended to be an instructional guide. To learn more
about specific operations,
seek
operators
manual by reading "how-to" books, trade magazines, or
websites.
OPERATIONS
Operation Overview
/components discussed later in this manual are
machine
not
read this entire manual and
additional training from experienced machine
, and do additional research outside of this
To complete a typical operation, the operator does the
following:
Examines workpiece to make sure it is within
1.
capacities of machine.
Adjusts rear work stop length for cut.
2.
3. Puts on safety glasses, leather boots, and leather
gloves.
Places workpiece on front extension arms.
4.
5. Slides workpiece under blade guard and upper blade,
and up against rear work stop.
6. Adjusts front work stop (or bevel gauge, if angled
workpiece) against workpiece to keep shearing force
from pushing workpiece forward.
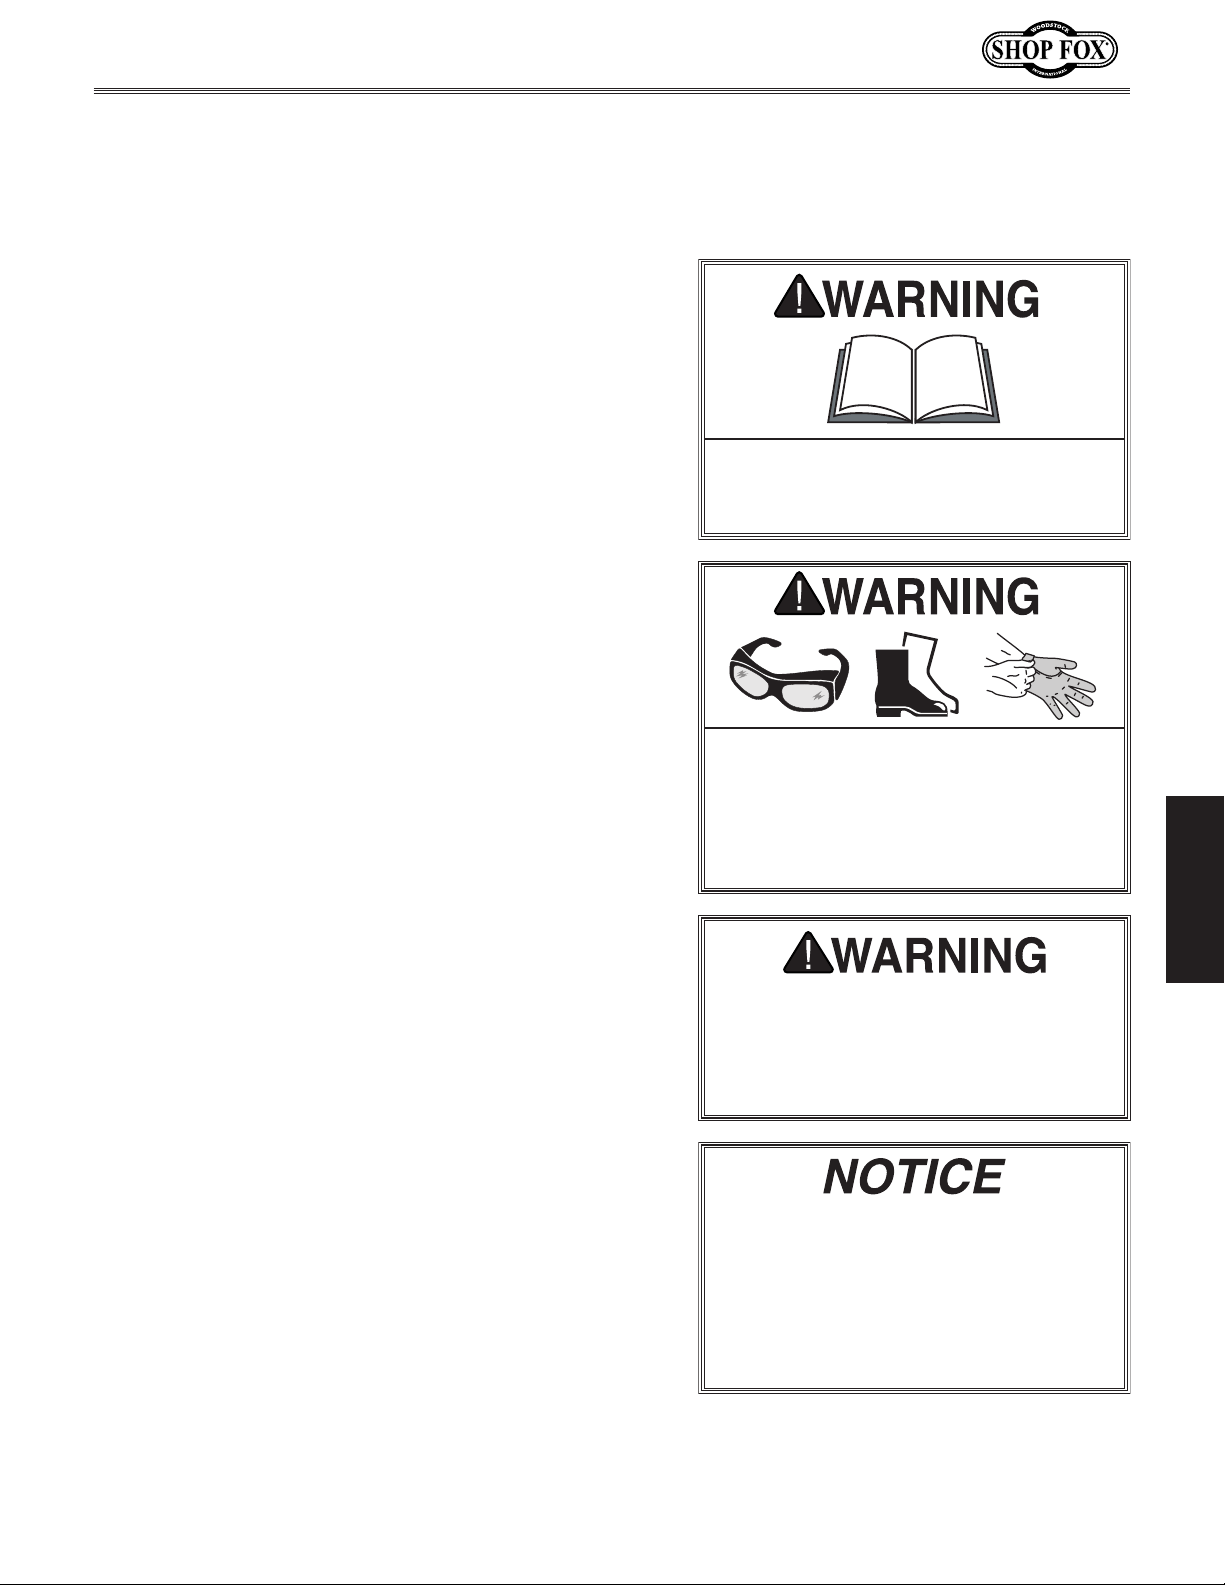
To reduce your risk of serious injury
or damage to the machine, read this
entire manual BEFORE using machine.
Bodily injury could result from using this
machine. Always wear safety glasses,
leather work boots, and heavy duty
leather work gloves when operating
this machine or whenever handling
sheet metal.
Shear blades or hold-down/blade guard
can easily pinch, crush, or amputate
fingers or other body parts. Always
keep body parts away from blades and
hold-down during operation.
OPERATIONS
With balanced and stable body position, firmly
7.
presses down on foot pedal to make cut.
Raises foot pedal and either removes workpiece or
8.
repeats Steps 5-7 to make additional cuts.
If you are an inexperienced operator,
we strongly recommend that you read
books or trade articles, or seek training
from an experienced operator of this
type of machinery before performing
unfamiliar operations. Above all, safety
must come first!
-19-
Page 22
Cutting Tips
• Never attempt to cut any workpiece narrower than
1
⁄2". The workpiece must be long enough to be
engaged by the hold-down/blade guard.
Model M1117 (For Machines Mfd. Since 9/21)
Shearing Action
• Keep the upper blade properly adjusted to the lower
blade (refer to Adjusting Blade Gap on Page 29 for
detailed instructions). This will help ensure good
cutting results and avoid blade damage.
Before each operation, clean cut-offs or debris away
•
from the shear.
• Use the foot pedal to engage the hold-down/blade
guard with the workpiece, then pause to check
the workpiece position. If the workpiece position
is correct, continue lowering the foot pedal to
complete the cut.
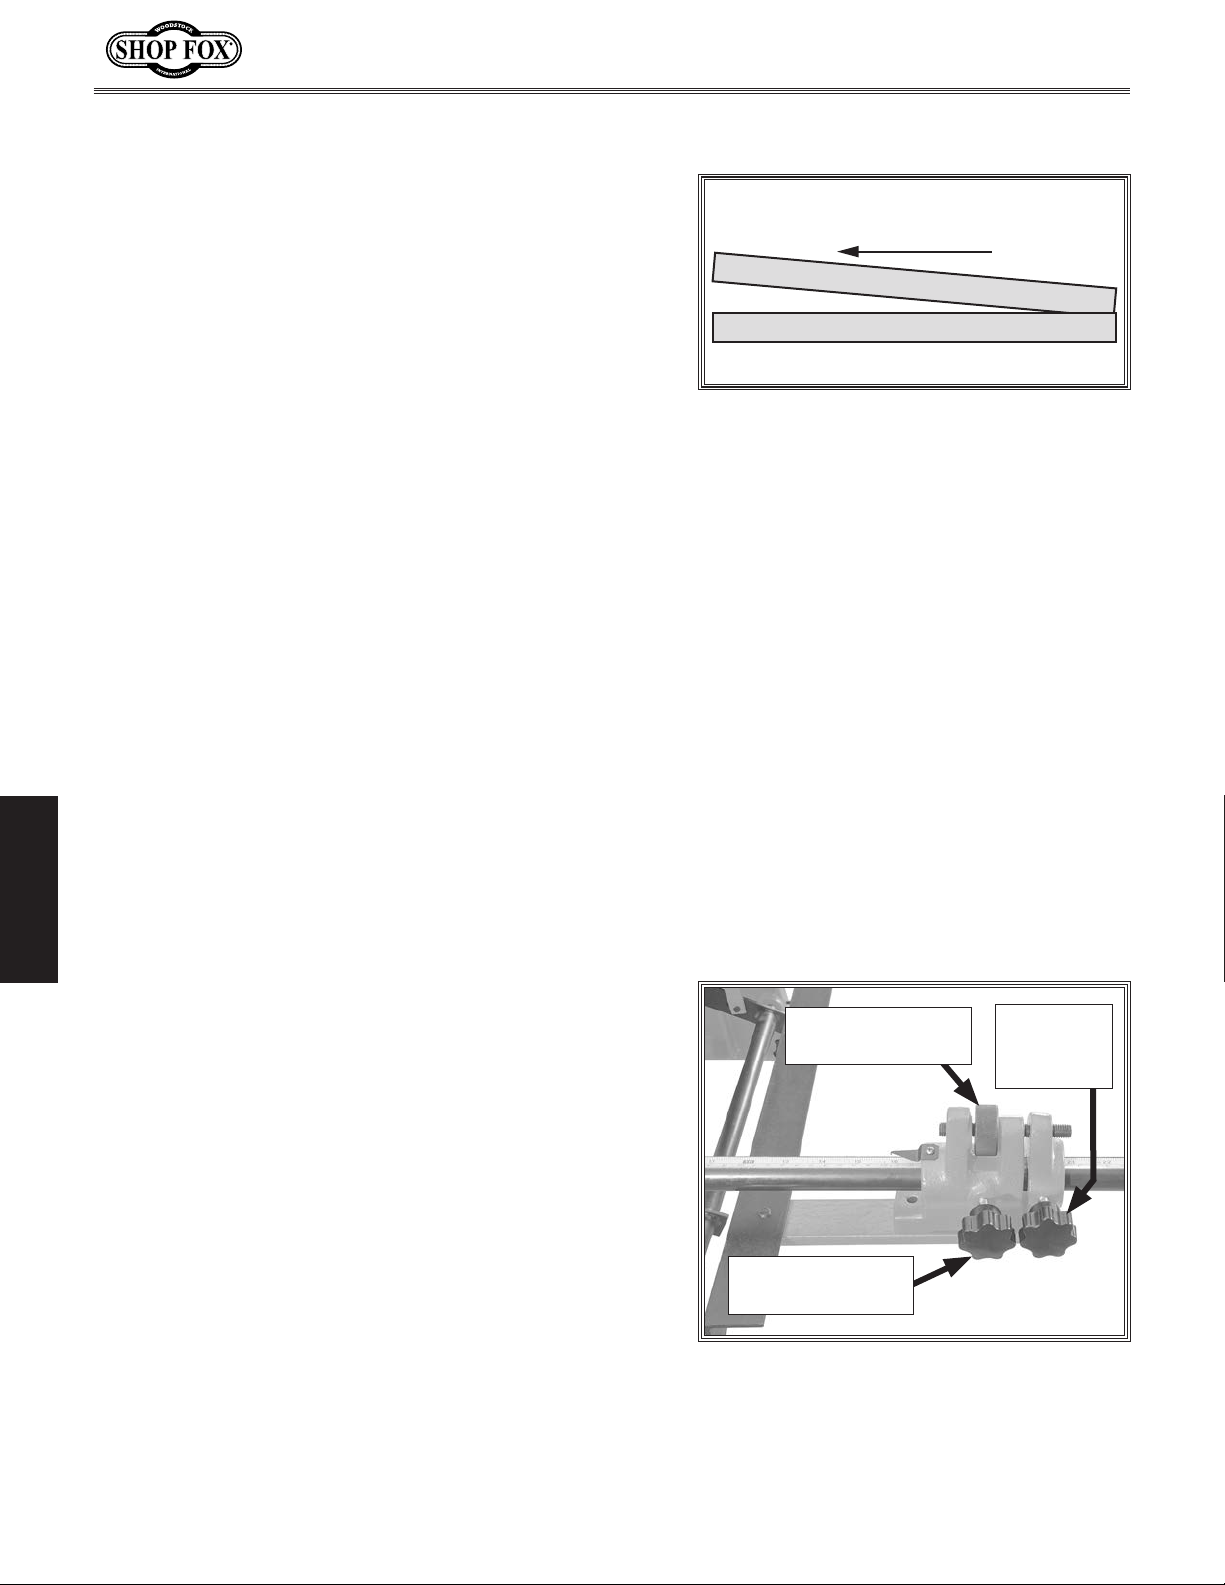
• The shearing action of the blades works similarly
to a pair of scissors (see illustration in Figure 17).
Use even pressure on the foot pedal throughout the
entire cut to produce a straight, even cut.
Adjusting Rear Work Stop
Upper Blade
Lower Blade
Figure 17. Blade shearing action.
The rear work stop is used for making repetitive cuts of
the same length. The micro-adjustment assemblies allow
for precise positioning of the work stop.
OPERATIONS
To adjust rear work stop, do these steps:
1. Loosen (2) rear work stop lock knobs and (2) micro-
adjustment lock knobs (see Figure 18).
. Slide rear work stop evenly along support rods so
2
work stop leading edge is at approximate desired
distance from cutting edges of blades.
Note: Use scales on top of support rods for
approximate positioning. Use fine ruler or tape
measure for more precise positioning.
. Use micro-adjustment knob on each assembly to
3
adjust work stop in small, precise amounts until they
are exactly where needed (see Figure 18).
Note: Move work stop evenly on both sides to keep
it parallel with the blades.
Micro-Adjustment
Knob
Micro-Adjustment
Lock Knob
Figure 18. Rear work stop adjustment
components.
Rear Work
Stop
Lock Knob
-20-
Page 23
Model M1117 (For Machines Mfd. Since 9/21)
4. Tighten micro-adjustment lock knobs to secure rear
work stop position.
Adjusting Front Work Stop
The front work stop keeps the shearing blades from
pushing the workpiece forward during cutting operations.
Use the following steps to adjust the front work stop
to the front workpiece edge once the workpiece has
been inserted under the blade guard and is ready to be
sheared.
To adjust front work stop, do these steps:
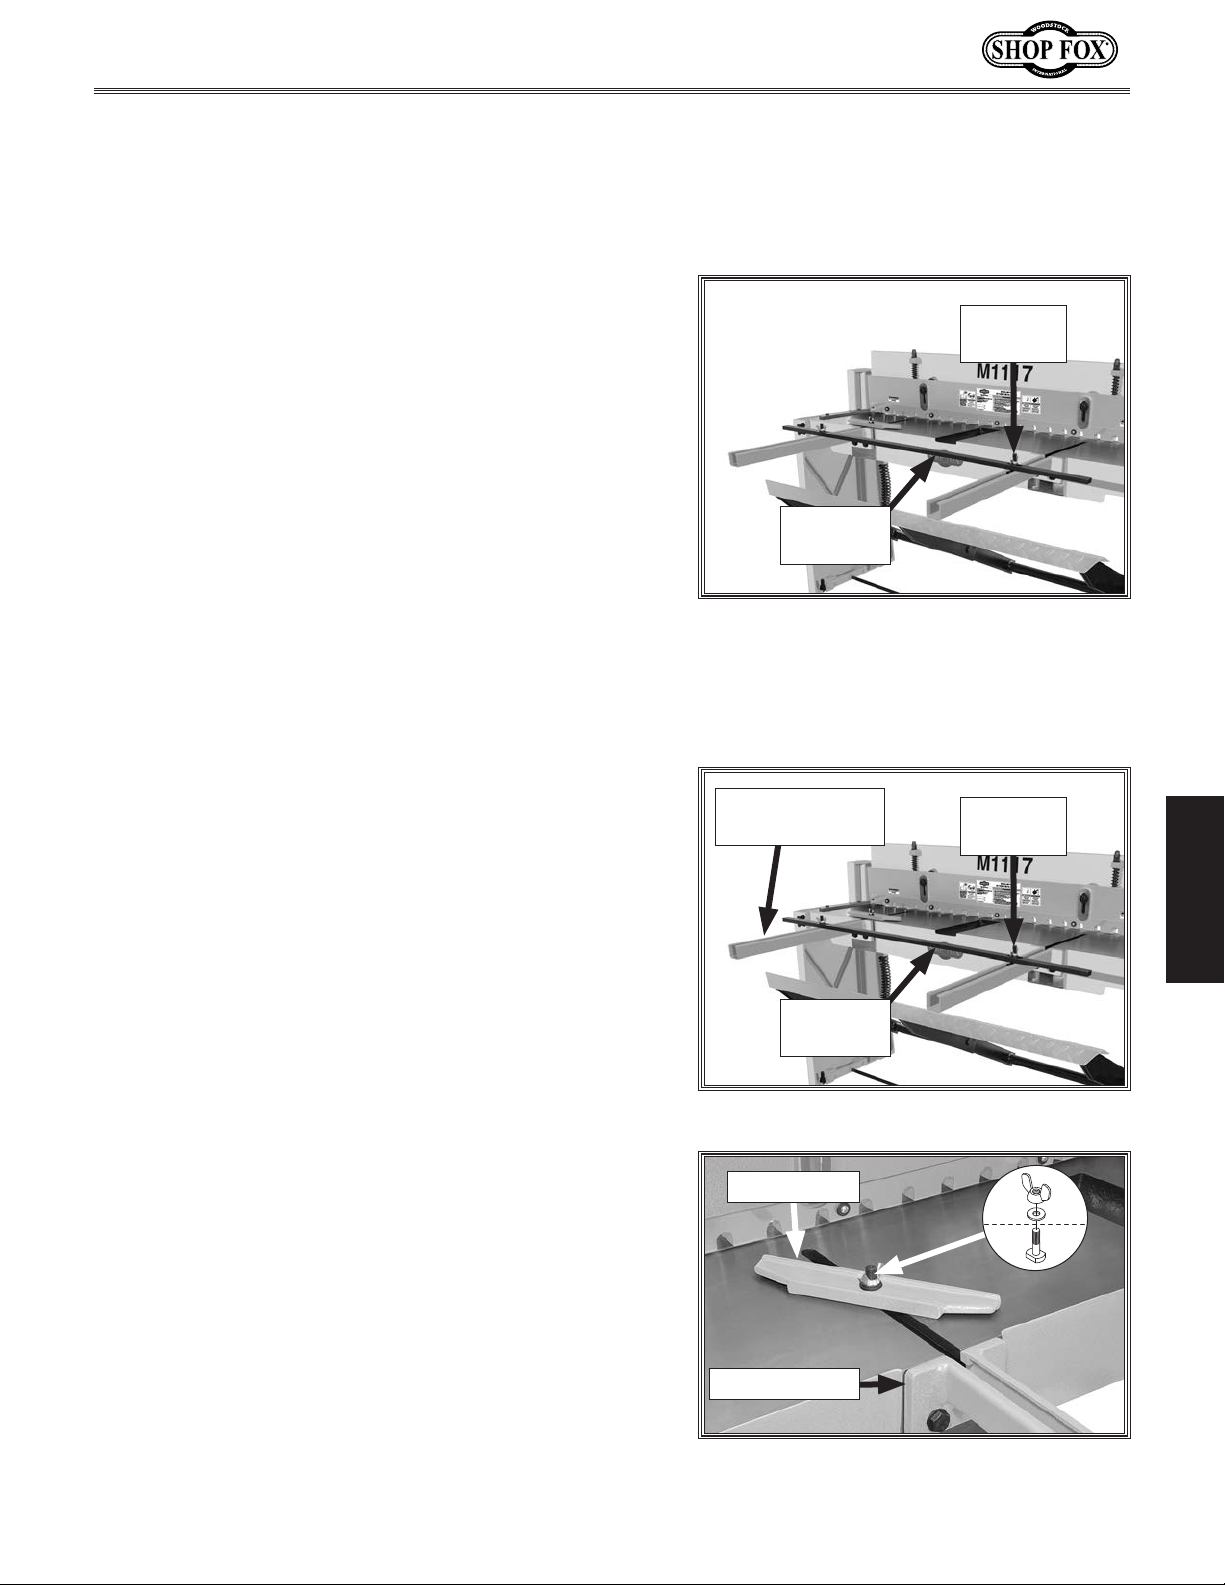
Wing Nut
(1 of 2)
1. Loosen (2) front work stop wing nuts (see
Figure 19).
. Adjust front work stop against front workpiece edge
2
and tighten wing nuts to secure.
Using Bevel Gauge
The bevel gauge can be installed in place of the front
work stop to support workpieces that have an angled
front edge.
To use bevel gauge, do these steps:
1. Loosen (2) front work stop wing nuts (see
Figure 20).
. Slide front work stop out of front extension arms to
2
remove (see Figure 20).
. Position workpiece on table and under blade guard
3
for shearing operation.
Front
Work Stop
Figure 19. Location of front work stop
wing nuts.
Front Extension
Arm (1 of 2)
Front
Work Stop
Figure 20. Front work stop components.
Wing Nut
(1 of 2)
OPERATIONS
4. Install (1) M12-1.75 x 45 T-bolt in T-slot and secure
bevel gauge to extension arm or table against
workpiece front edge with (1) 12mm flat washer and
M12-1.75 wing nut (see Figure 21).
Note: Figure 21 shows bevel gauge installed in left
T-slot, but it can be installed in either side. Install
the bevel gauge in the best position to secure your
workpiece for the operation.
-21-
Bevel Gauge
Extension Arm
Figure 21. Bevel gauge installed to
support angled front workpiece edge.
Page 24
Model M1117 (For Machines Mfd. Since 9/21)
ACCESSORIES
Metal Shear Accessories
The following accessories may be available through your local Woodstock International Inc. Dealer. If you
do not have a dealer in your area, these products are also available through online dealers. Please call
or e-mail Woodstock International Inc. Customer Service to get a current listing of dealers at: 1-800-8408420 or at [email protected].
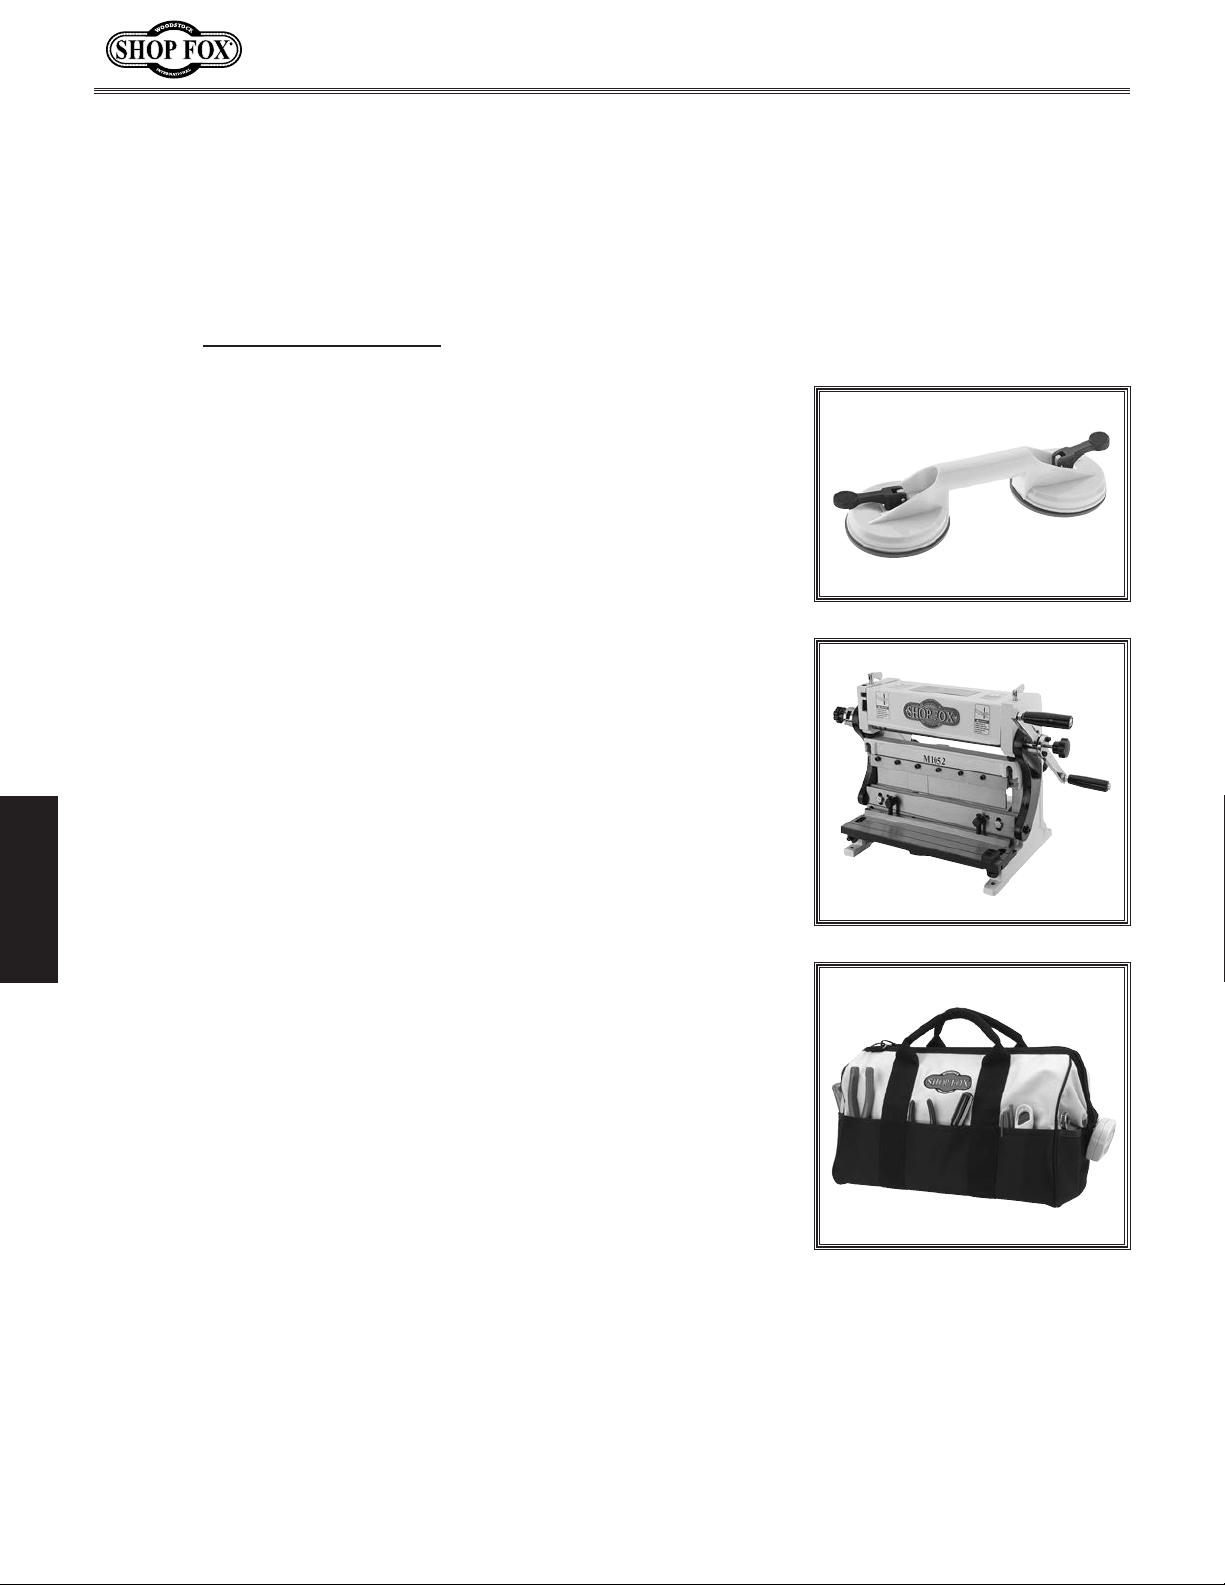
D3042 Double Suction Cup handles plate glass, glass mirrors,
The
and sheet metal with safety and security. Cam-action levers make
placement and removal quick and easy.
The M1052 3-In-1 Sheet Metal Machine has a 12" wide capacity
and three sheet metal functions in one unit. There is no need to
spend extra money and tie up shop space with three single-use
machines. You will love the convenience and accuracy of this do-itall machine! Maximum capacity of 22 gauge and a roll diameter of
1
⁄2".
1
OPERATIONS
The D3269 Deluxe Shop Tool Bag is perfect for the mobile
craftsman who has a tool for everything. The deluxe shop bag
features 18 easy access pockets, ballistic nylon construction, huge
carrying capacity and a detachable shoulder strap that quickly clips
on or off. Interior measures 17" L x 9
and fully opened.
1
⁄2" W and 12" when unzipped
-22-
Page 25
Model M1117 (For Machines Mfd. Since 9/21)
The D2273 Single Roller Stand features convenient hand knobs
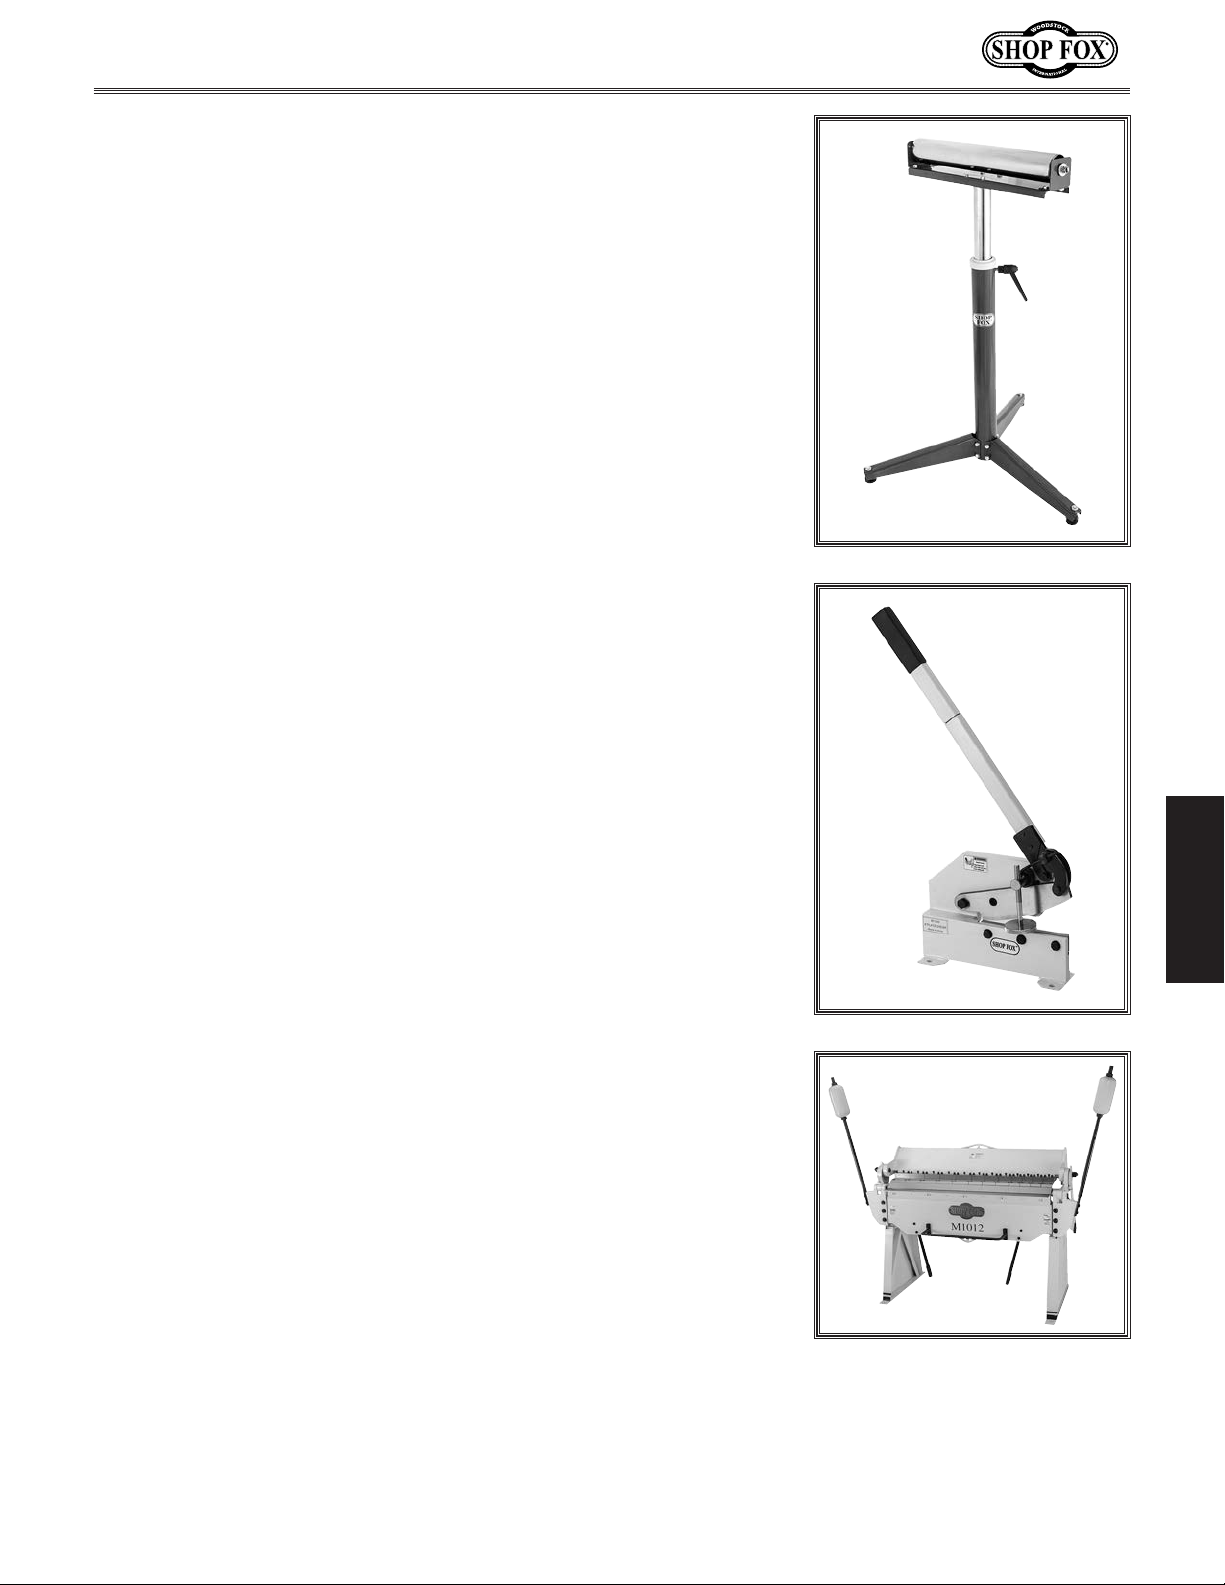
for fast height adjustment. The super heavy-duty roller stand is
invaluable for supporting work on machines of varying heights.
The M1040 8" Plate Shear and M1041 12" Plate Shear are the
fastest way to cut sheet metal, plate stock, and round stock to size.
Both of these shears can be mounted for stationary use and feature
compound lever action for tremendous mechanical advantage. Plate
3
capacity:
⁄16" (7 gauge).
The M1012 48" Pan and Box Brake is great for forming extra-wide
or long pieces of sheet metal. When bolted to a concrete floor, the
M1012 bends boxes or pans up to 6" deep, material up to 48" wide,
and 12-gauge thick mild steels, from 0-135 degrees! Removable and
adjustable 3", 4", and 25" fingers can accommodate a variety of
metal widths.
OPERATIONS
-23-
Page 26
MAINTENANCE
General
For optimum performance from this machine, this
maintenance schedule must be strictly followed.
Ongoing
To minimize your risk of injury and maintain proper
machine operation, stop operations immediately if you
ever observe any of the items below, and fix the problem
before continuing operations:
• Loose mounting bolts.
• Loose or damaged blade guard.
• Worn or damaged blades.
• Loose or bent rear work stop support rods.
• Any other unsafe condition.
Model M1117 (For Machines Mfd. Since 9/21)
Daily Maintenance
• Clean and protect blades and bare cast iron
surfaces.
• Lubricate pivot points.
Weekly Maintenance
• Lubricate shearing blades, gibs, and slides.
Cleaning & Protecting
Cleaning the Model M1117 is relatively easy. Use a brush
to clear away any metal debris from the blades, the blade
guard, and the table.
Protect the unpainted cast iron table and blades by wiping
with regular applications of quality metal protectant.
MAINTENANCE
-24-
Page 27
Model M1117 (For Machines Mfd. Since 9/21)
Lubrication
There are a number of parts on this machine that undergo
a lot of movement and must remain lubricated for smooth
operation and long life.
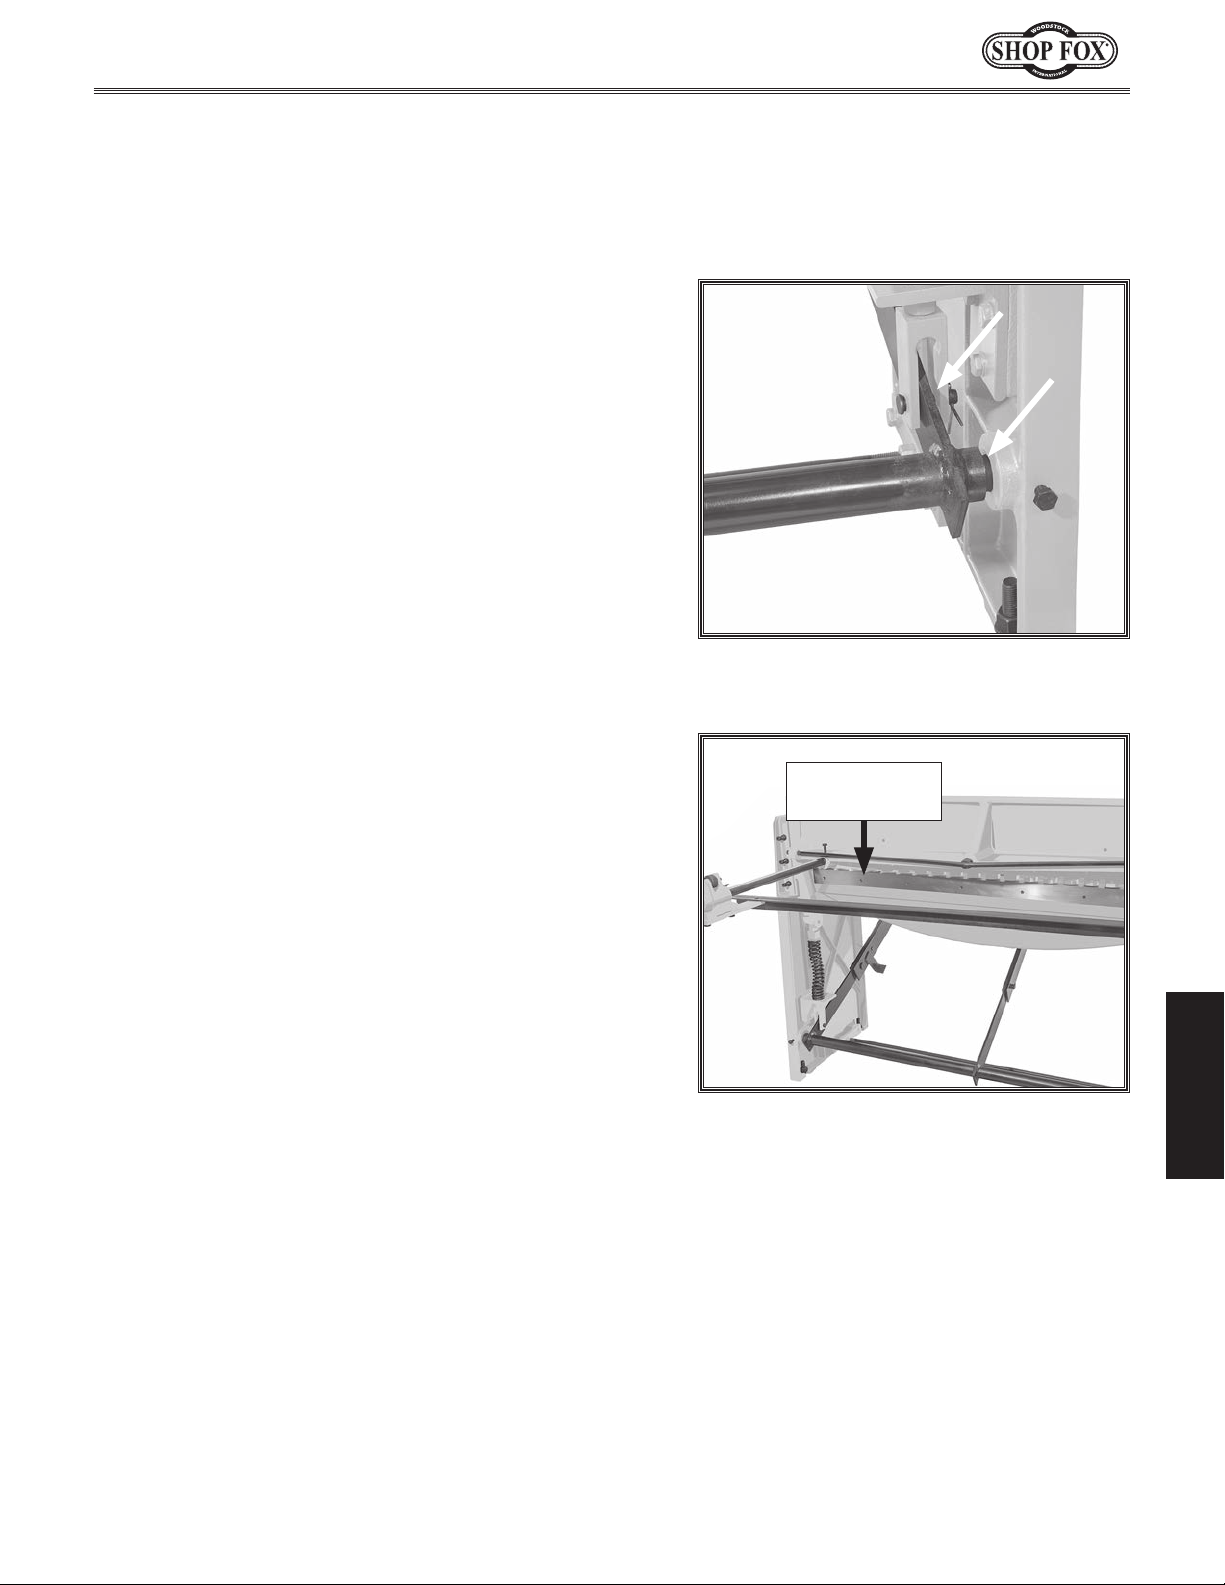
Pivot Pins
Oil Type .......................................ISO 32 Equivalent
Oil Amount
Lubrication Frequency
Items
Wire Brush
Shop Rags
Light Machine Oil or ISO 32 Equivalent.......... As Needed
Use a wire brush to clean any built-up grease from pivot
pins (see Figure
lubricant to the exposed portions of all four pivot pins.
Keep your hands and fingers away from shearing area and
press down on the foot pedal a few times to distribute
the lubricant.
............................................ 1–2 Drops
.................................... Daily
Needed Qty
.......................................................1
............................................ As Needed
22) before applying a few drops of
Figure 22. Location of pivot pins (2 of 4
shown).
Shearing Blades
Oil Type .......................................ISO 68 Equivalent
Oil Amount
Lubrication Frequency
Items
Protective Gloves
Shop Rags
Mineral Spirits
Light Machine Oil or ISO 68 Equivalent.......... As Needed
While wearing protective gloves, use a rag and mineral
spirits to clean away grease and built-up grime from the
surfaces of the shearing blades (see Figure
blades are dry, apply oil to the surfaces with a clean rag.
............................................ 1–2 Drops
................................. Weekly
Needed Qty
...........................................1 Pr.
............................................ As Needed
....................................... As Needed
23). Once the
Surface of
Shearing Blade
MAINTENANCE
Figure 23. Location of lower shearing
blade surface.
-25-
Page 28
Gibs & Slides
Oil Type .......................................ISO 68 Equivalent
Oil Amount
Lubrication Frequency
Item
Needed Qty
Light Machine Oil or ISO 68 Equivalent.......... As Needed
............................................ 1–2 Drops
................................. Weekly
Model M1117 (For Machines Mfd. Since 9/21)
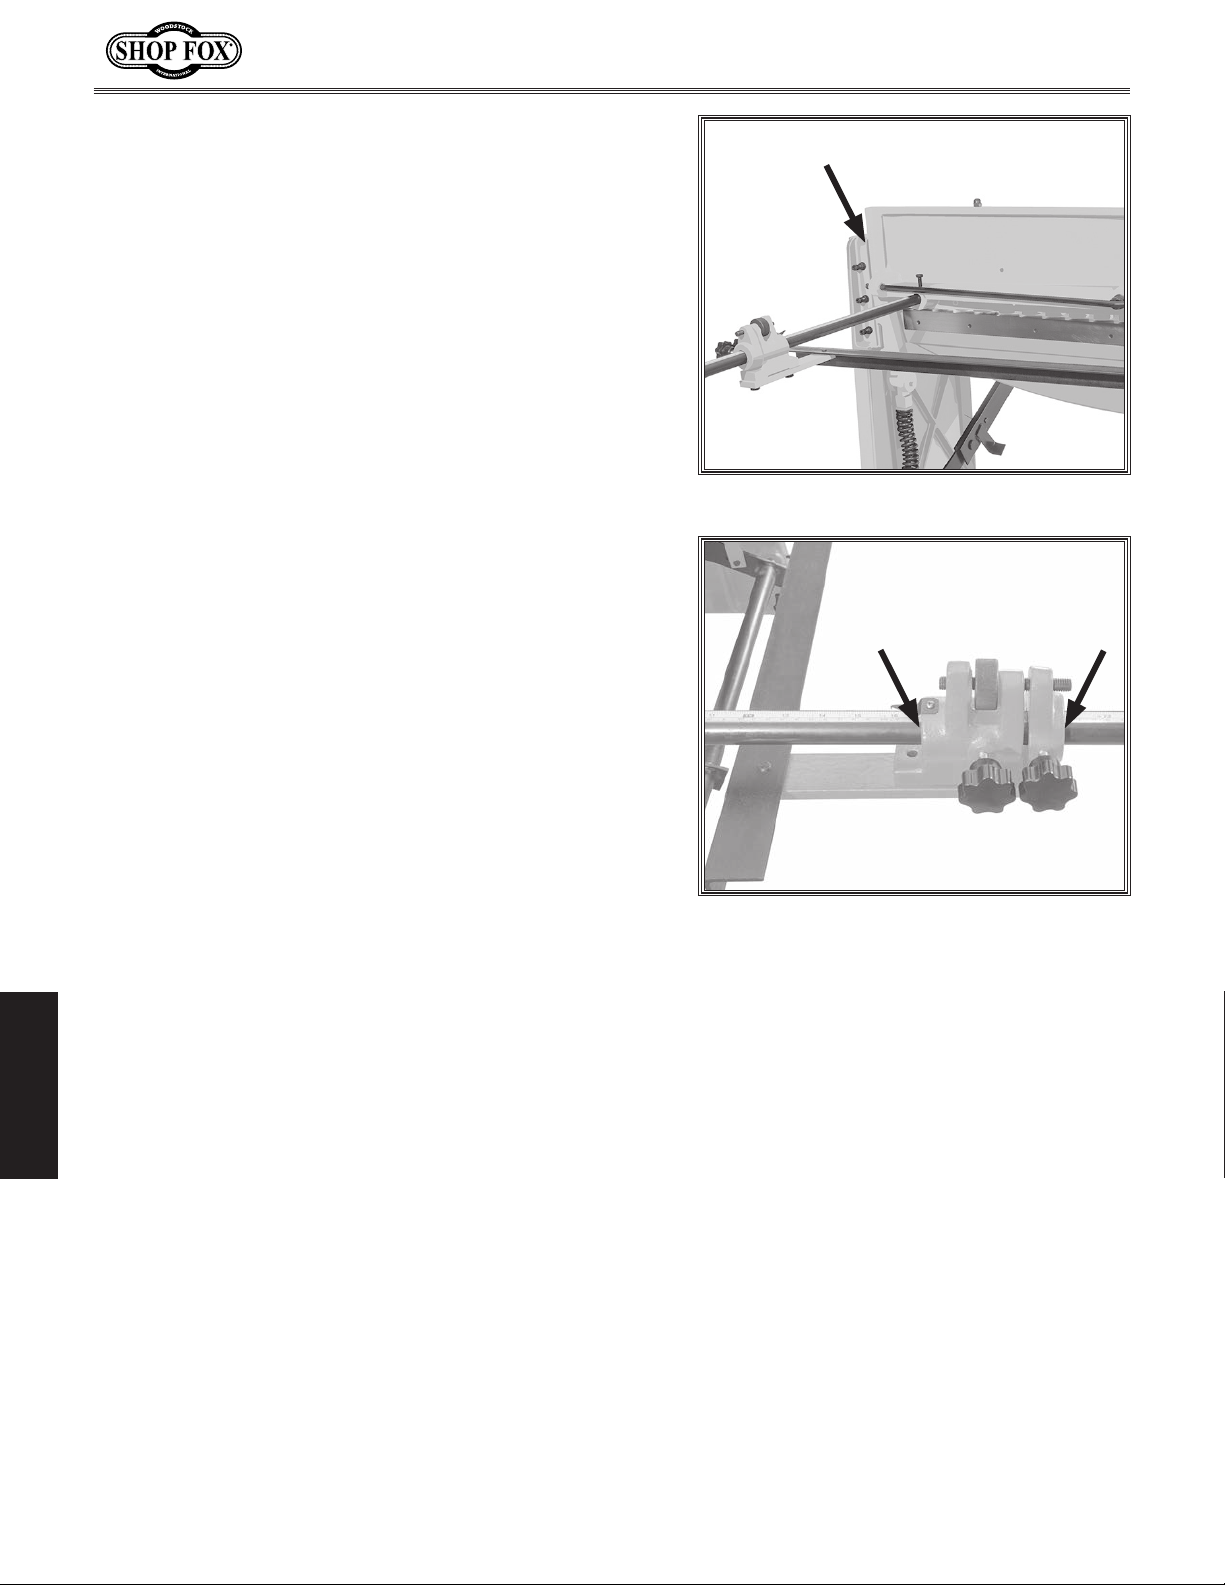
Apply a few drops of oil at each gib (see Figure
weekly to keep the upper blade and hold-down/blade
guard moving smoothly.
24)
Rear Work Stop Assemblies
Oil Type .......................................ISO 68 Equivalent
Oil Amount
Lubrication Frequency
Items
Shop Rags
Mineral Spirits
Light Machine Oil or ISO 68 Equivalent.......... As Needed
The rear work stop assemblies must slide smoothly in
order to achieve accurate measurements when shearing.
Clean the rear work stop support rods with mineral
spirits when you have any trouble adjusting the rear
work stop position. Apply a few drops of oil to the
locations shown in Figure
............................................ 1–2 Drops
............................. As Needed
Needed Qty
............................................ As Needed
....................................... As Needed
25 on each assembly.
Figure 24. Gib and slide lubrication point.
Figure 25. Rear work stop assembly
lubrication locations.
MAINTENANCE
-26-
Page 29
Model M1117 (For Machines Mfd. Since 9/21)
This section covers the most common service adjustments
or procedures that may need to be made during the life
of your machine.
If you require additional machine service not included
in this section, please contact Woodstock International
Technical Support at (360) 734-3482 or send e-mail to:
[email protected].
SERVICE
General
Adjusting Gibs
The gibs are responsible for the amount of play in
the upper blade. They should only be adjusted if the
foot pedal is difficult to lower or if all the other blade
adjustment have been verified as correct, and the quality
of cut is still poor.
Tools Needed Qty
Hex Wrench 8mm ...............................................1
Open-End Wrench 17mm.......................................1
To adjust gibs, do these steps:
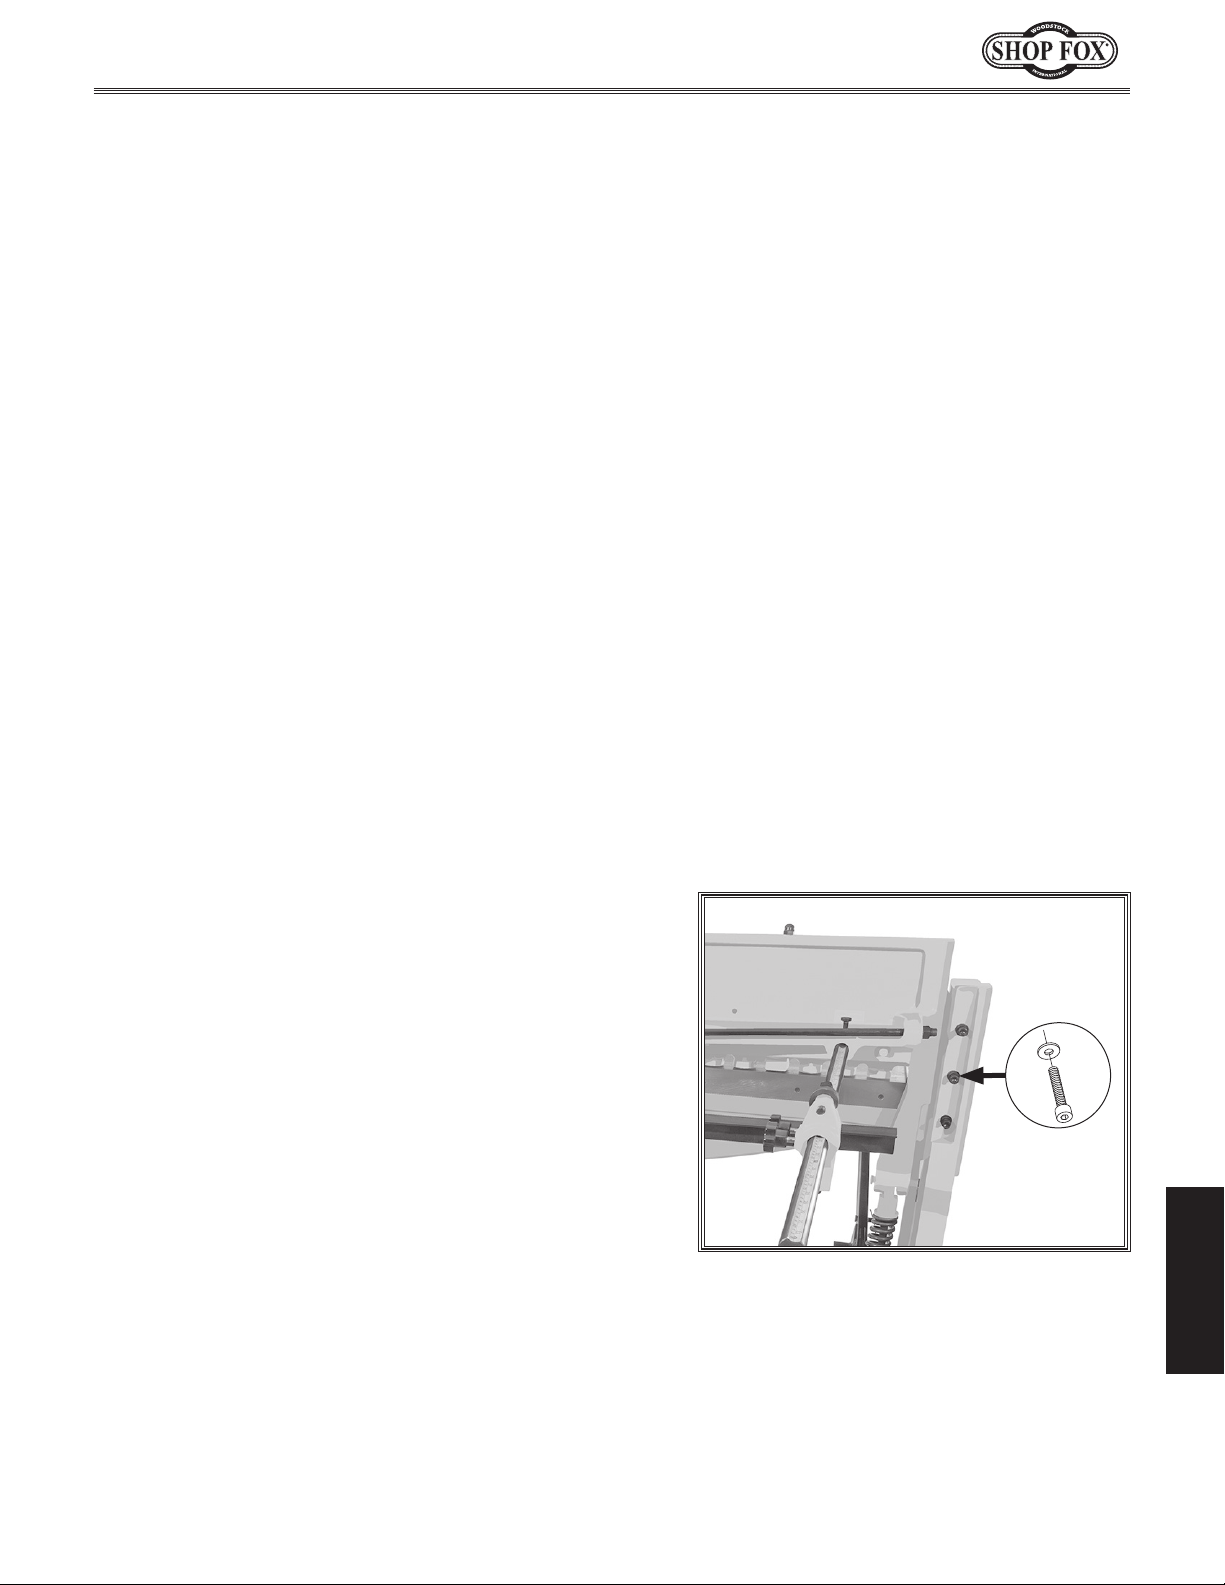
. Loosen (3) jam nuts on each gib (see Figure 26).
1
. Adjust (3) gib screws on each side of shear in small,
2
equal increments (see Figure 26). Test for binding or
play after each adjustment by pushing or pulling top
of cutter bar.
— If foot pedal is difficult to lower and blades are
binding, adjust screws counterclockwise.
— If too much play of in upper blade is resulting in
poor quality of cuts, adjust screws clockwise.
. Tighten jam nuts to secure gib adjustments.
3
x 3
SERVICE
Figure 26. Location of gib screws and jam
nuts.
-27-
Page 30
Sharpening/Replacing
Blade
The upper blade of the Model M1117 has two cutting
edges so that if one cutting edge becomes dull, you can
reverse the blade and use the fresh, sharp cutting edge.
If both the upper blade cutting edges are dull, or the
cutting edge of the lower blade is dull, sharpen the
blade(s) on a surface grinder and make sure the blade is
flat along the entire length. Re-sharpen each blade edge
as needed until it is too thin to safely install (as described
in the following steps), then replace the blade. We
recommend you keep an extra set of blades on hand to
avoid any downtime.
Items Needed Qty
Another Person ..................................................1
Protective Gloves (For Each Person)
Hex Wrench 8mm
Surface Grinder
Mineral Spirits
Shop Rags
Metal Protectant
New Upper Blade (#XM1117024)
New Lower Blade (#XM1117025).................. As Needed
............................................ As Needed
...............................................1
.................................................1
....................................... As Needed
.................................... As Needed
.....................1 Pr.
.................. As Needed
Model M1117 (For Machines Mfd. Since 9/21)
Shear blades are sharp. Wear protective
gloves when handling blades to prevent
laceration injuries.
x 8
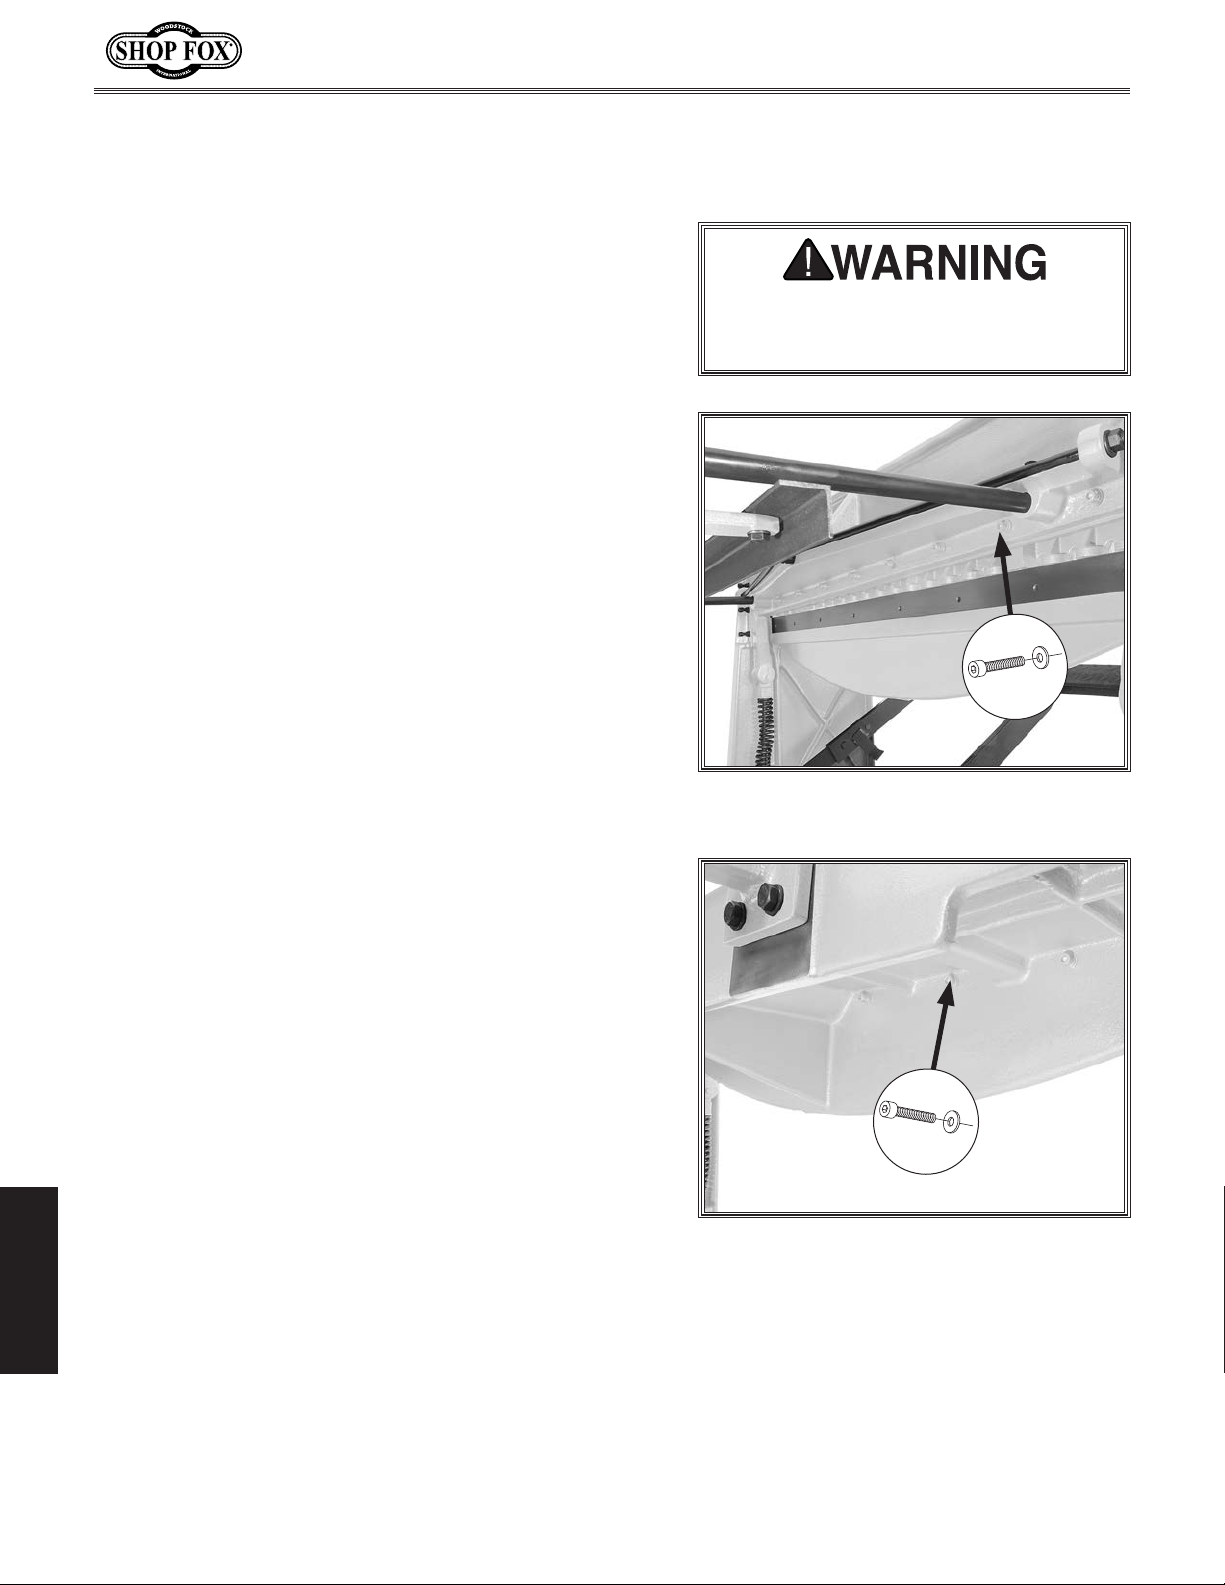
Figure 27. Upper blade cap screws and
flat washers.
To sharpen/replace blade, do these steps:
1. Have another person support blade while you remove
(8) cap screws and flat washers to remove blade (see
Figures 27-28).
. Reverse blade (upper blade only) or sharpen on a
2
surface grinder.
. Clean blade with mineral spirits, then apply thin
3
coat of quality metal protectant.
. Install blade using hardware removed in Step 1.
4
— If blade is so thin after sharpening that securing
cap screws extend beyond opposite side of cutting
edge, replace blade.
SERVICE
x 8
Figure 28. Lower blade cap screws and
flat washers.
-28-
Page 31
Model M1117 (For Machines Mfd. Since 9/21)
Adjusting Blade Gap
The gap between the upper and lower blades (as they
pass each other) must remain even along the length of
the blades to produce clean cuts. Initially, this adjustment
has been made at the factory. However, over time and
with normal wear, you may need to adjust the blade gap.
If the blade gap is too wide, the workpiece will not cut
correctly and show signs of bending, ripping, or tearing.
If the blade gap is too narrow, the upper blade will bind
when lowering past the lower blade and the cutting edges
may become damaged.
Items Needed Qty
Scrap Paper .......................................... As Needed
Wrench or Socket 24mm
Open-End Wrenches 17mm
Feeler Gauge 0.002"
.......................................1
....................................2
............................................1
To adjust blade gap, do these steps:
1. Make cuts on piece of paper along full length of
shear blades.
— If paper cuts cleanly on full length of shear blades,
blade gap requires no adjustment.
— If paper does not cut cleanly on only one end of
shear, lower blade needs to be adjusted on that
end. Proceed to Step 2.
— If paper does not cut cleanly along the entire
length of blades, both ends of lower blade need to
be adjusted. Proceed to Step 2.
— If paper cuts cleanly on ends but not center of
blades, or it cuts cleanly in center but not ends,
blade bow needs to be adjusted (refer to Adjusting
Blade Bow on Page 30 for detailed instructions).
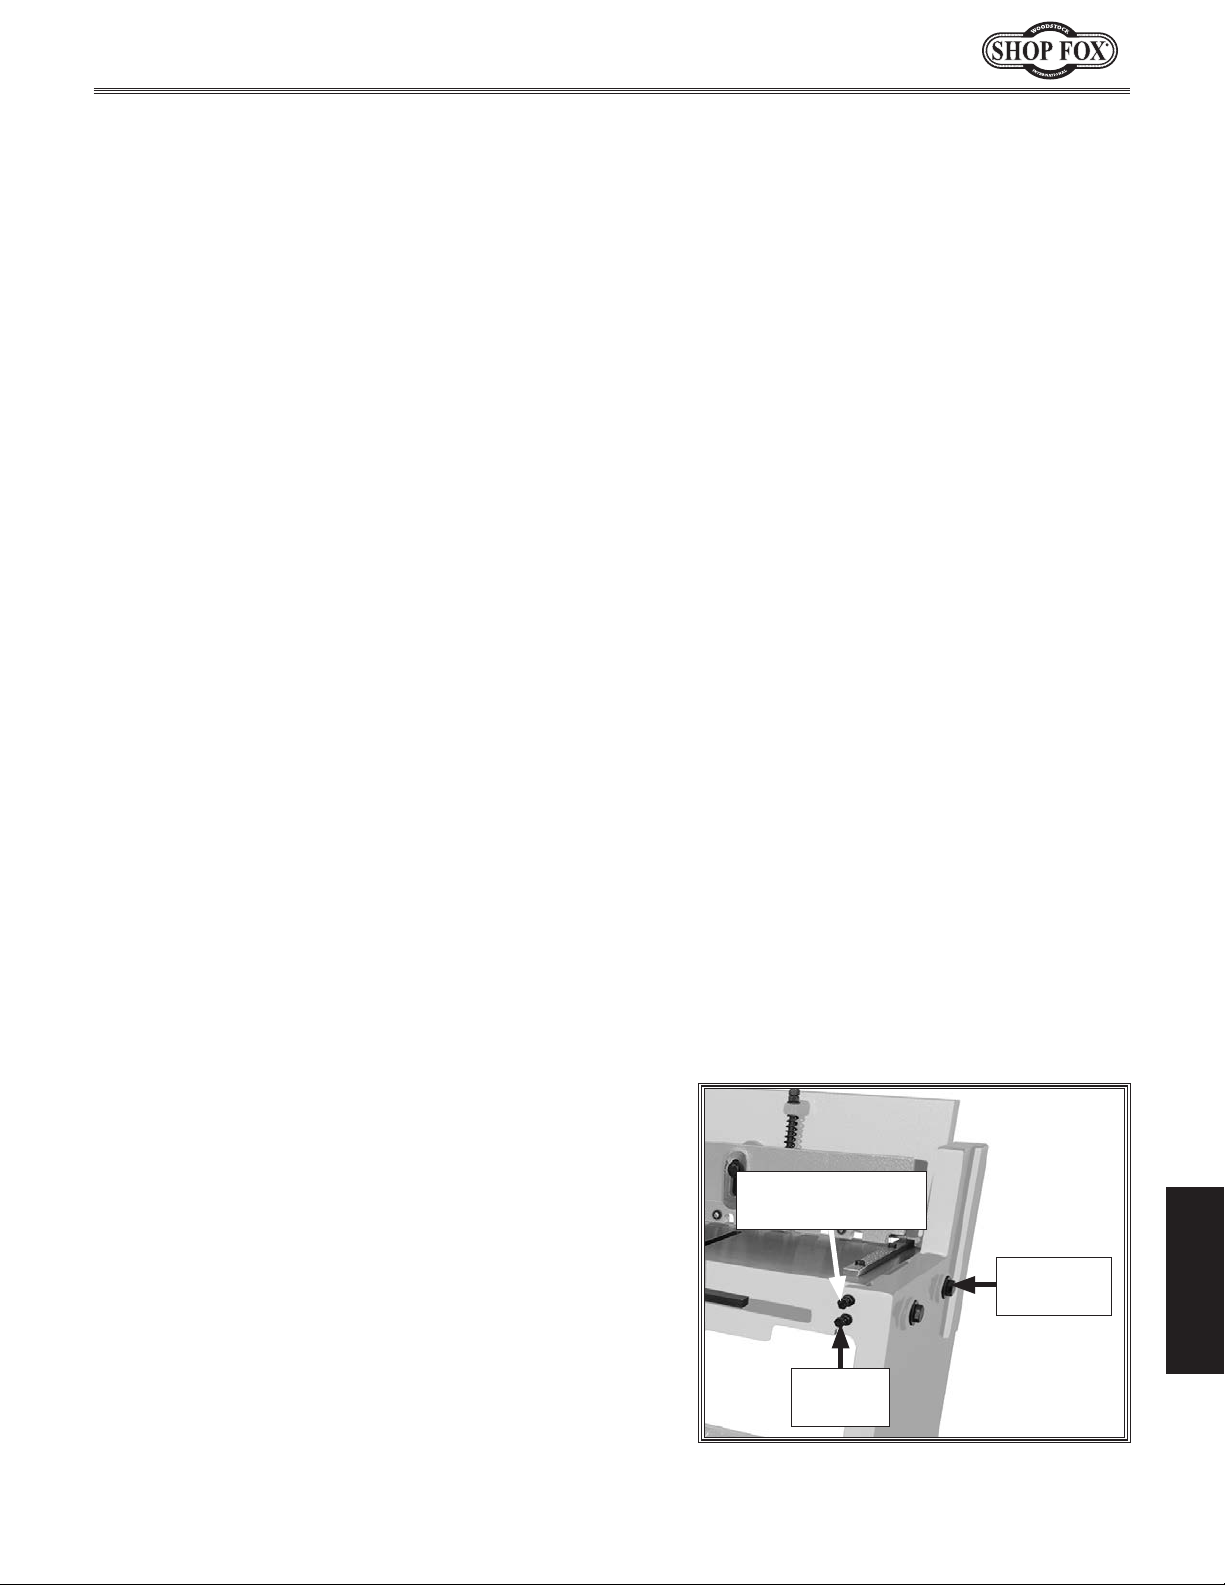
. Loosen (2) table bolts, (2) table adjustment bolts,
2
and (2) jam nuts on side of shear that needs
adjustment (see Figure 29).
. Use foot pedal to lower and hold upper blade in
3
lowest position.
Table Adjustment
Bolt (1 of 2)
SERVICE
Table Bolt
(1 of 2)
. Insert feeler gauge between blades on side that
4
needs adjustment, then turn table adjustment bolts
to move table and lower blade until lower blade
makes light contact with feeler gauge against upper
blade.
Jam Nut
(1 of 2)
Figure 29. Location of blade gap
adjustment components.
-29-
Page 32
5. Tighten (2) jam nuts and (2) table bolts to secure
blade gap adjustment.
. Repeat Step 1 to check adjustment.
6
— If paper still does not cut cleanly, but blade gap
adjustment is correct, blade(s) may need to be
sharpened (refer to Sharpening/Replacing Blade
on Page 28 for detailed instructions).
Adjusting Blade Bow
The blade bow is used to keep the upper blade straight
along its full length by adjusting the amount of force that
the bow exerts on the blade ends.
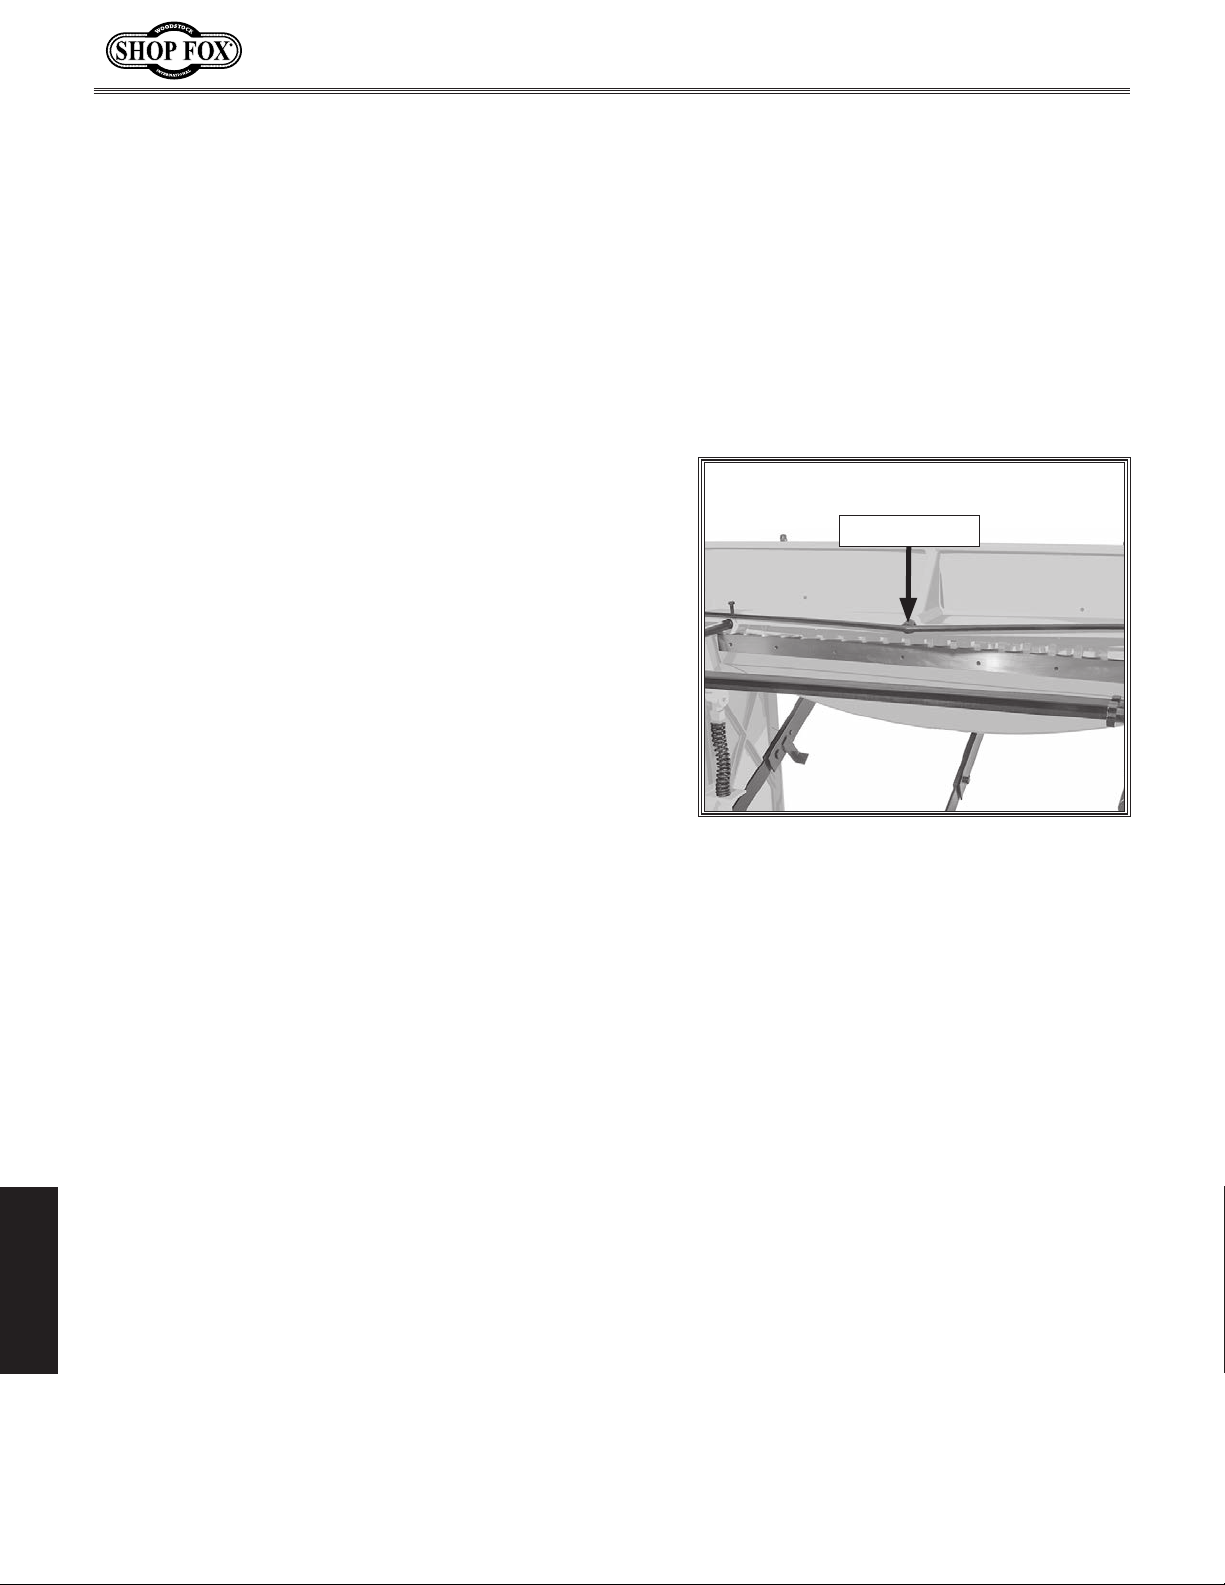
The blade bow is adjusted by adjusting the bow jam nut
on the centering rod (see Figure 30).
Model M1117 (For Machines Mfd. Since 9/21)
Bow Jam Nut
Items Needed Qty
Open-End Wrench 24mm.......................................1
Scrap Paper
To adjust blade bow, do these steps:
1. Perform Step 1 of Adjusting Blade Gap on Page 29
to determine if blade needs bow adjustment. Adjust
blade gap, if necessary, before proceeding.
— If paper cuts cleanly on ends but not center of
— If paper cuts cleanly on center but not end of
.......................................... As Needed
blades, adjust bow jam nut clockwise while testing
results until paper cuts cleanly along entire length
of blades.
blades, adjust bow jam nut counterclockwise while
testing results until paper cuts cleanly along entire
length of blades.
Figure 30. Location of bow jam nut.
SERVICE
-30-
Page 33
Model M1117 (For Machines Mfd. Since 9/21)
Adjusting
Return Spring Tension
The tension of the return springs can be adjusted to
increase or decrease the return rate.
Tool Needed Qty
Open-End Wrench 24mm.......................................1
To adjust return spring tension, do these steps:
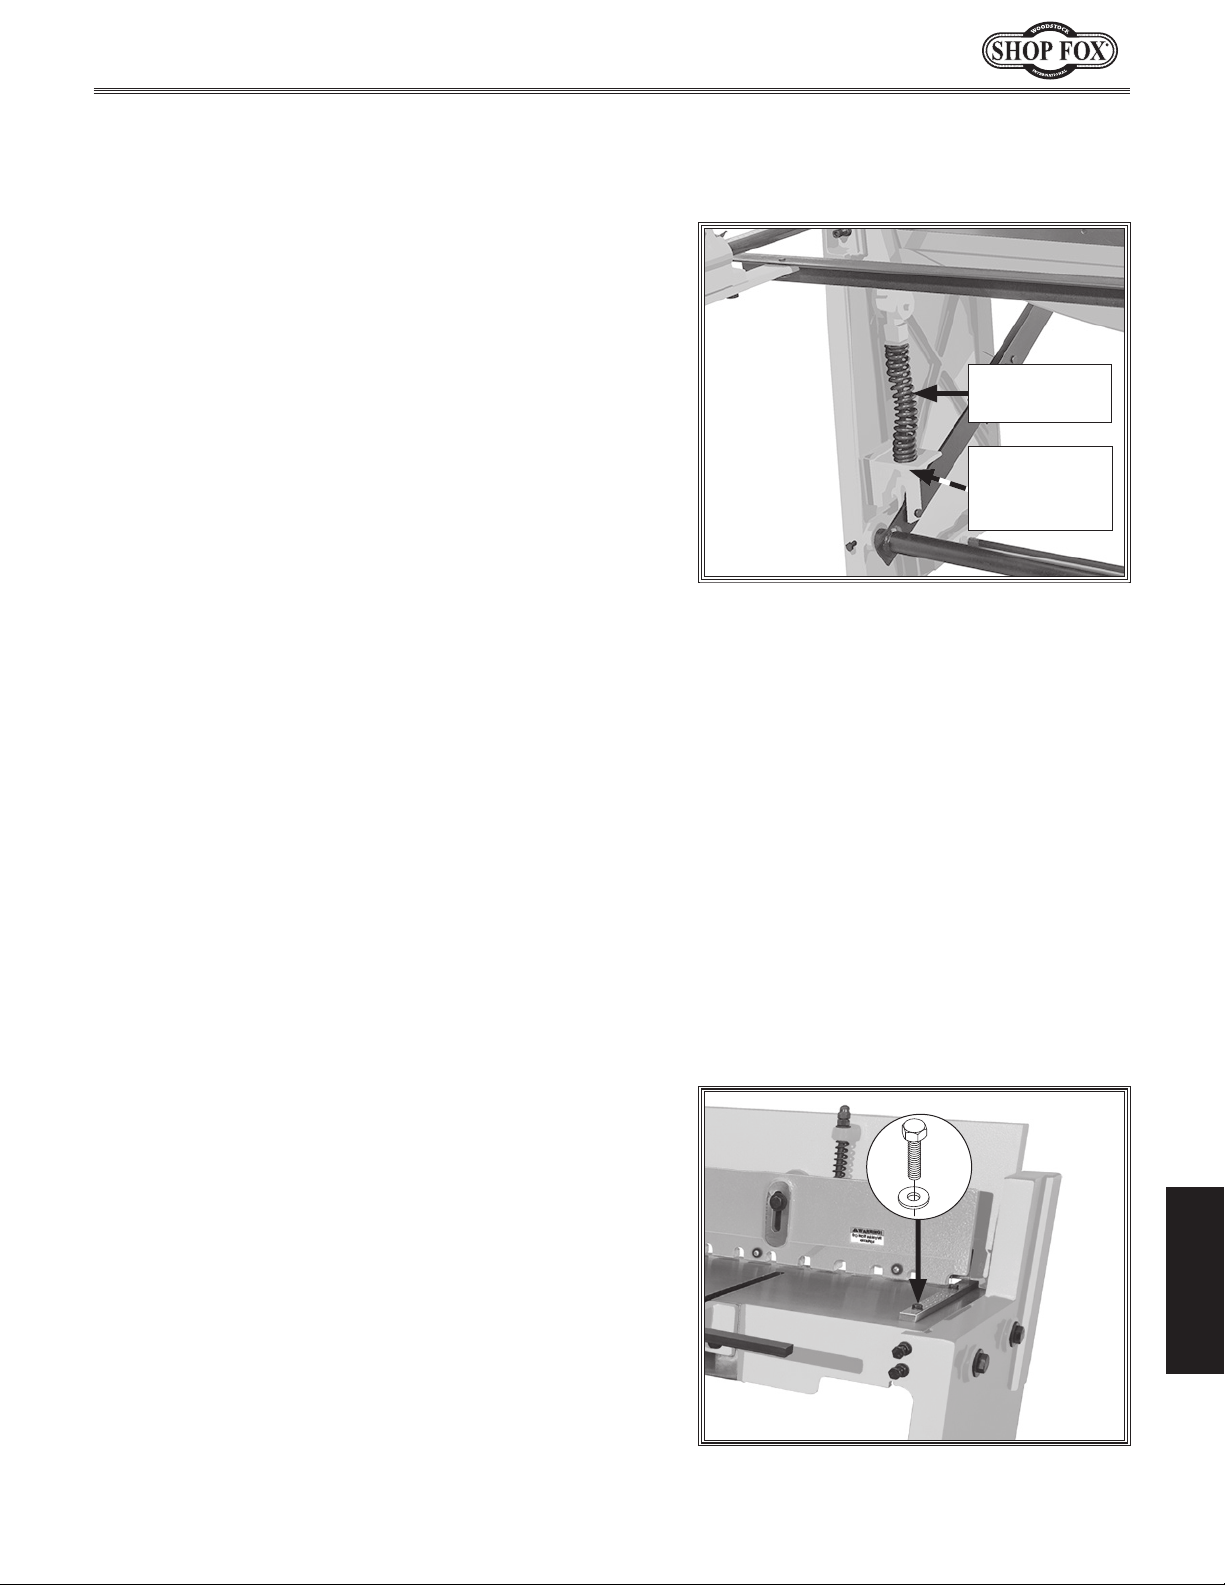
1. Adjust (2) return spring hex nuts in small, equal
increments (see Figure 31).
— To increase return rate, tighten hex nuts against
springs.
— To decrease return rate, loosen hex nuts.
Squaring Front Scales
For the front scales to work properly, these scales must
be square to the blades.
Tools Needed Qty
Machinist's Square ..............................................1
Wrench or Socket 13mm
To square front scales, do these steps:
.......................................1
Return Spring
(1 of 2)
Return Spring
Hex Nut
(1 of 2)
Figure 31. Return spring tension
adjustment components.
1. Use foot pedal to lower and hold blade guard in
lowest position.
. Place machinist's square against blade guard and
2
front scale.
— If scale is square to blade guard, no adjustment is
necessary.
— If scale is not square to blade guard, proceed to
Step 3.
. Loosen (2) hex bolts for front scale that needs
3
adjustment (see Figure 32).
. Place one side of machinist's square against blade
4
guard and adjust front scale against other side of
square.
. Tighten hex bolts from Step 3 to secure position.
5
-31-
x 2
SERVICE
Figure 32. Location of front scale hex
bolts.
Page 34
Adjusting
Hold-Down/Blade Guard
When the upper blade is lowered, the blade guard is also
engaged to contact and secure the workpiece during the
cutting operation. The blade guard must be parallel with
the table to correctly secure workpieces.
Tools Needed Qty
Feeler Gauge Set ...............................................1
Wrench or Socket 19mm
Adjusting Blade Guard Clearance
For an extra thin or thick workpiece, the guard can be
adjusted for the correct amount of clearance to secure it.
To adjust blade guard clearance, do these steps:
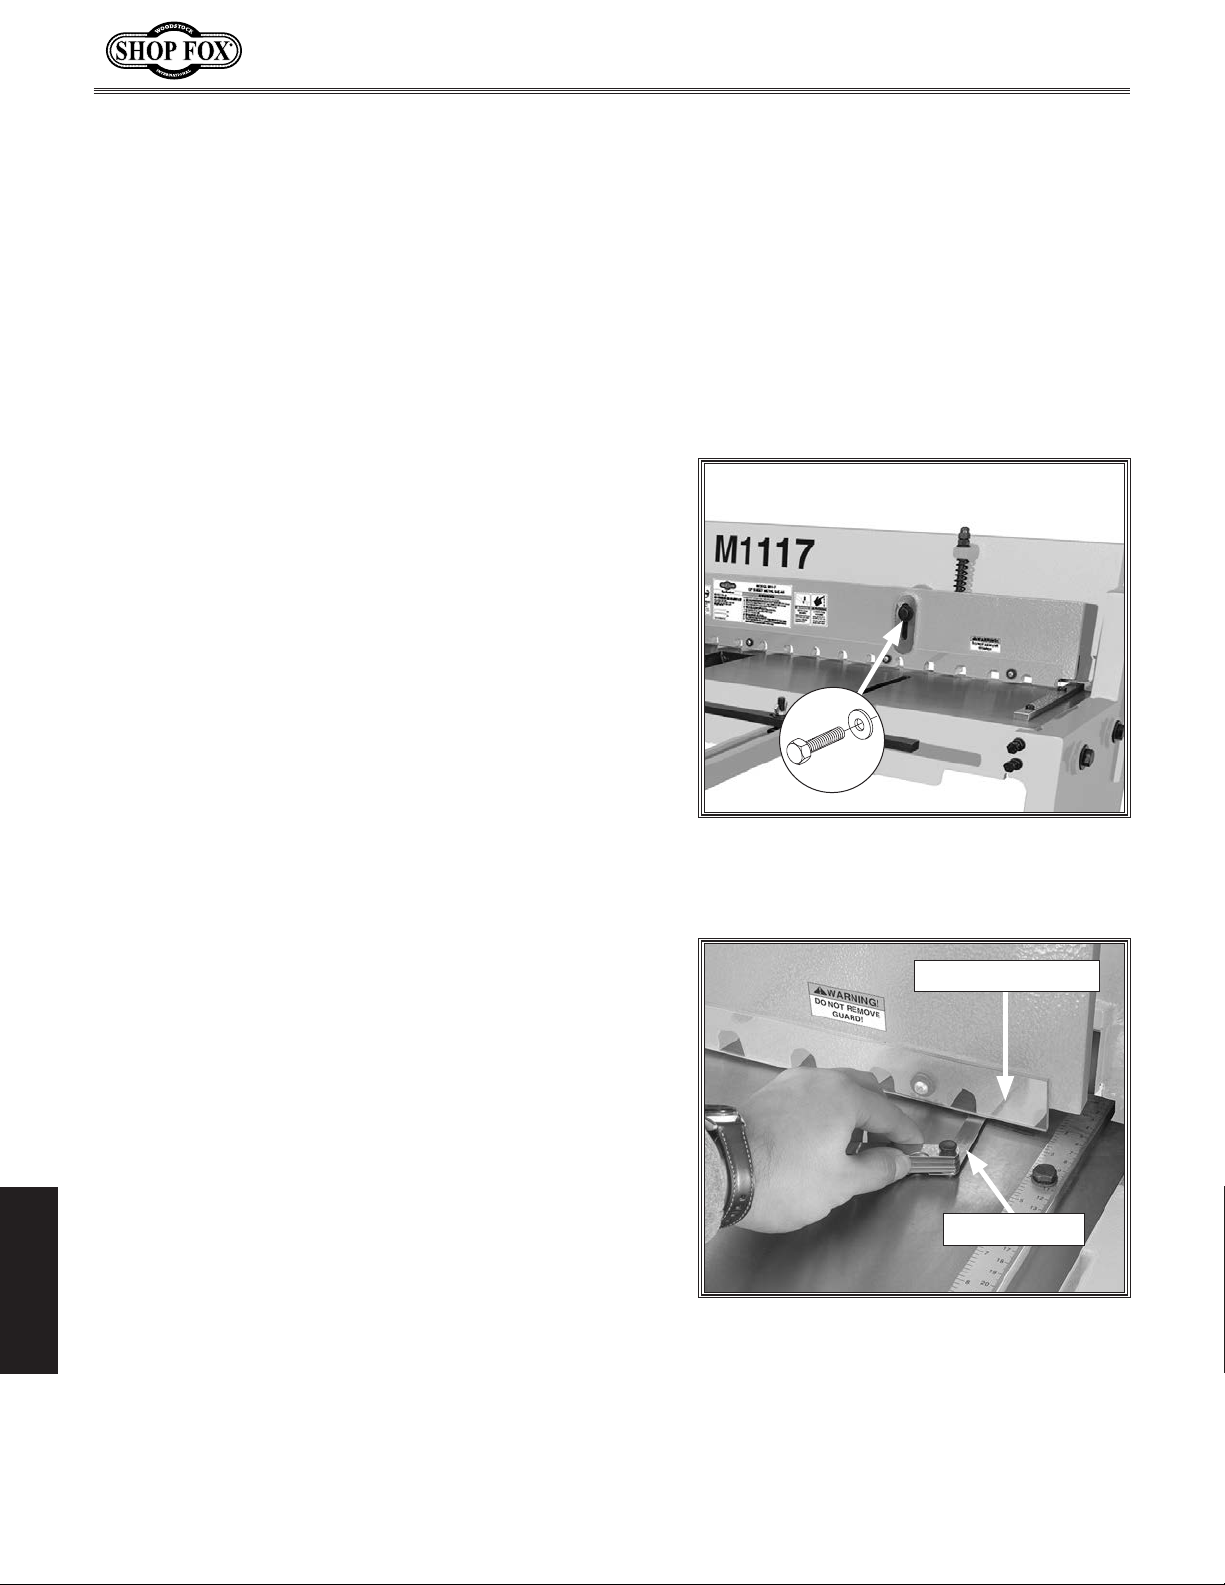
1. Loosen (2) blade guard hex bolts (see Figure 33).
.......................................1
Model M1117 (For Machines Mfd. Since 9/21)
. Adjust blade guard up or down to accommodate
2
workpiece thickness.
. Tighten (2) blade guard hex bolts to secure.
3
. Place edge of workpiece under blade guard, then use
4
foot pedal to confirm workpiece is secured by guard.
. Refer to following section to verify guard parallelism.
5
Adjusting Blade Guard Parallel With Table
1. Use foot pedal to lower and hold blade guard in
lowest position.
. Insert largest feeler gauge that will fit between
2
hold-down finger and table on right end of blade
guard (see Figure 34).
. Repeat Step 2 on left end of blade guard.
3
— If both hold-down fingers are same distance from
table, no adjustment is required.
x 2
Figure 33. Location of blade guard hex
bolts.
Hold-Down Finger
Feeler Gauge
— If both hold-down fingers are not same distance
SERVICE
4
5
from table, proceed to Step 4.
. Loosen blade guard hex bolt on side of blade guard
that needs adjustment.
. Adjust blade guard until entire length is same
distance from table, then tighten hex bolt.
-32-
Figure 34. Using feeler gauge to check
blade guard clearance.
Page 35
Model M1117 (For Machines Mfd. Since 9/21)
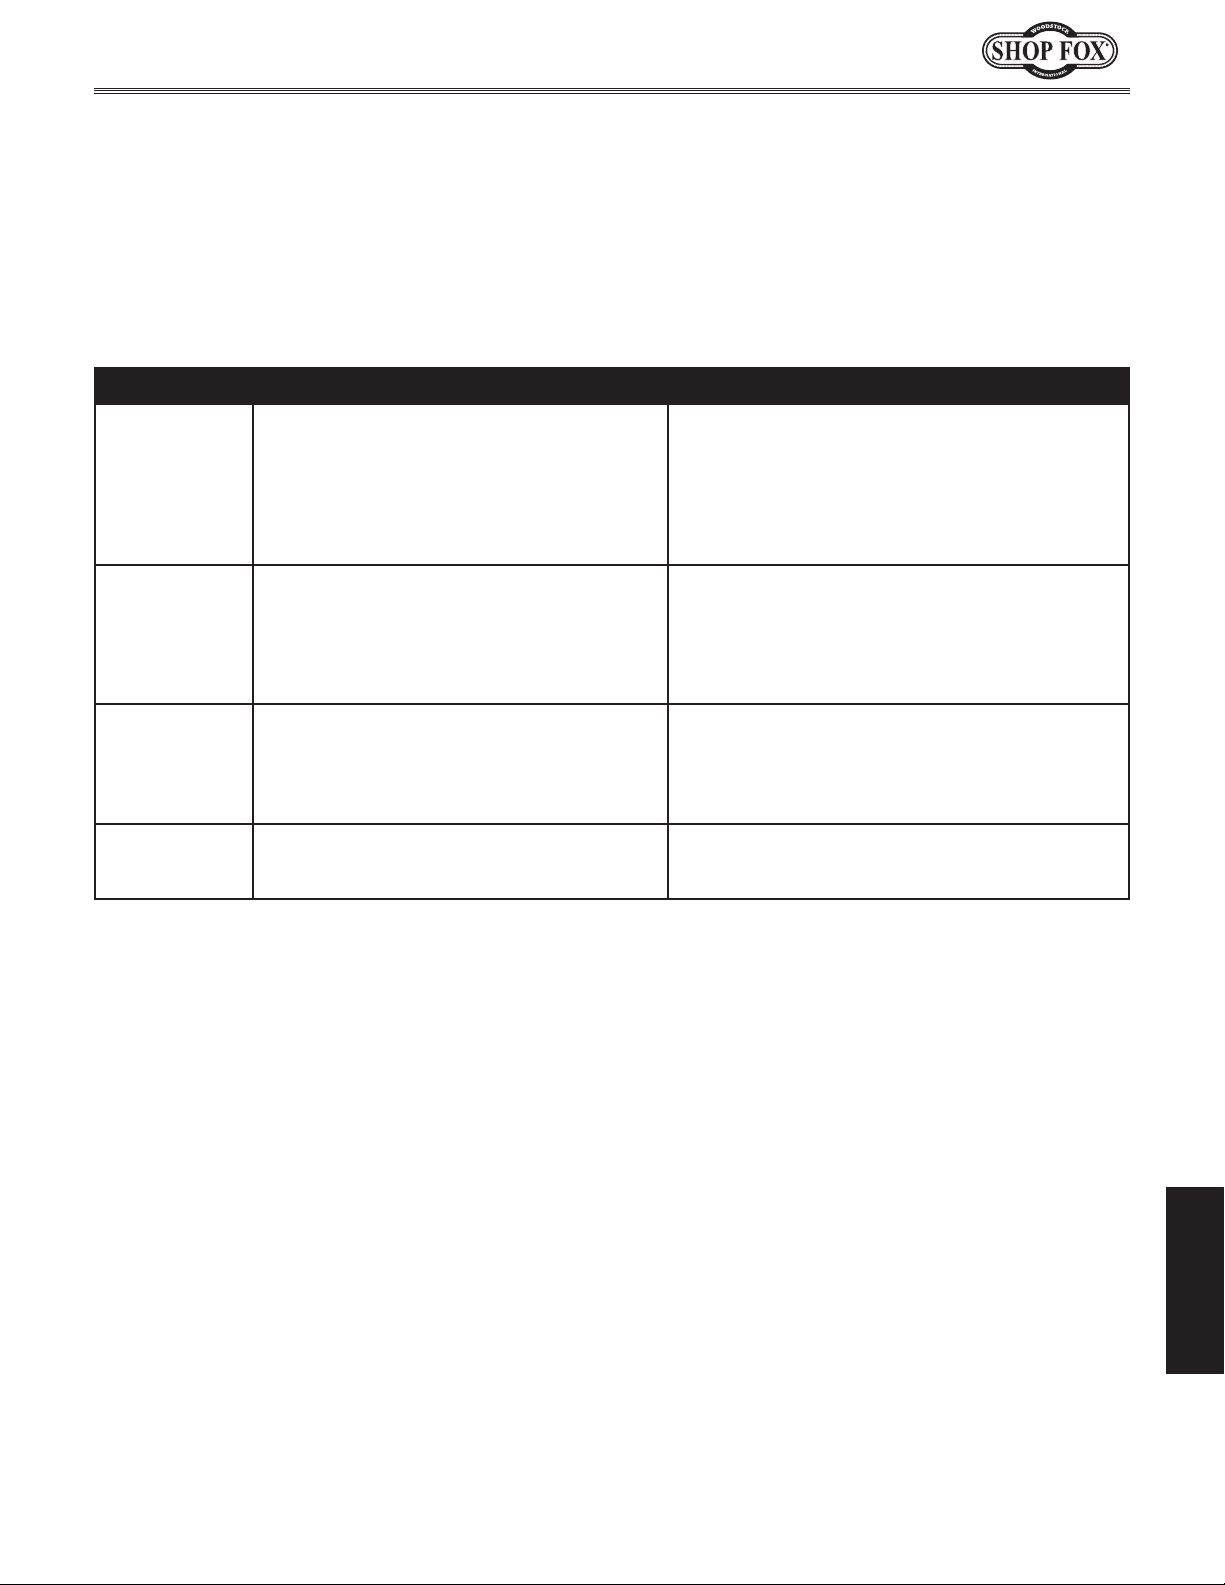
The following troubleshooting tables cover common problems that may occur with this machine. If you
need replacement parts or additional troubleshooting help, contact our Technical Support.
Note:
available, your original purchase receipt. This information is required to properly assist you.
Troubleshooting
Before contacting Tech Support, find the machine serial number and manufacture date, and if
Operations
PROBLEM POSSIBLE CAUSE CORRECTIVE ACTION
Shear will not
cut workpiece.
Cuts are not
square.
Poor quality of
cuts (ripping or
tear ing).
Foot pedal
difficult to use.
1. Workpiece thickness exceeds shear capacity.
2. Not enough pressure applied to foot pedal.
3. Blades worn or damaged.
4
. Blade gap not correct.
5
. Hold-down/blade guard is not adjusted
correctly.
1. Rear work stop is not parallel with blades.
2. Blade gap not correct.
3. Blade bow is not correct.
4
. Hold-down/blade guard is not adjusted
correctly.
1. Blade gap not correct.
2. Blades worn or damaged.
3. Hold-down/blade guard is not adjusted
correctly.
4
. Gibs too loose.
1. Blade gap not correct.
2. Pivot pins need lubrication.
3. Gibs too tight.
1. Only use workpiece material that is within shear
capacity (Page 3).
2. Safely increase pressure on foot pedal.
3. Sharpen/replace blades (Page 28).
4
. Properly adjust blade gap (Page 29).
5
. Properly adjust hold-down/blade guard (Page 32).
1. Properly adjust rear work stop parallel with blades
(Page 20).
2. Properly adjust blade gap (Page 29).
3. Properly adjust blade bow (Page 30).
4
. Properly adjust hold-down/blade guard (Page 32).
1. Properly adjust blade gap (Page 29).
2. Sharpen/replace blades (Page 28).
3. Properly adjust hold-down/blade guard (Page 32).
4
. Tighten gib screws (Page 27).
1. Properly adjust blade gap (Page 29).
2. Lubricate pivot pins (Page 25).
3. Loosen gib screws (Page 27).
-33-
SERVICE
Page 36
33
19
68
18
53
20
50
72
5
52
57
67
56
54
21
50
22
76
39
76
71
17
23
56
20
16
42
41
42
33
73
20
58
Model M1117 (For Machines Mfd. Since 9/21)
PARTS
Main
74
72
75
6
12
52
32
55
15
48
49
14
45
56
1
43
74
46
77
72
7
44
13
27
76
47
29
57
47
31
24
67
44
51
23
46
2
50
39
76
10
38
41
42
42
3
17
19
11
62
61
59
34
72
37
39
9
8
12
14
15
33
20
48
18
43
45
25
22
28
20
70
40
26
8
9
33
21
4
66
63
20
58
68
78
69
65
65
60
20
64
68
35
36
31
76
51
32
53
PARTS
-34-
Page 37
Model M1117 (For Machines Mfd. Since 9/21)
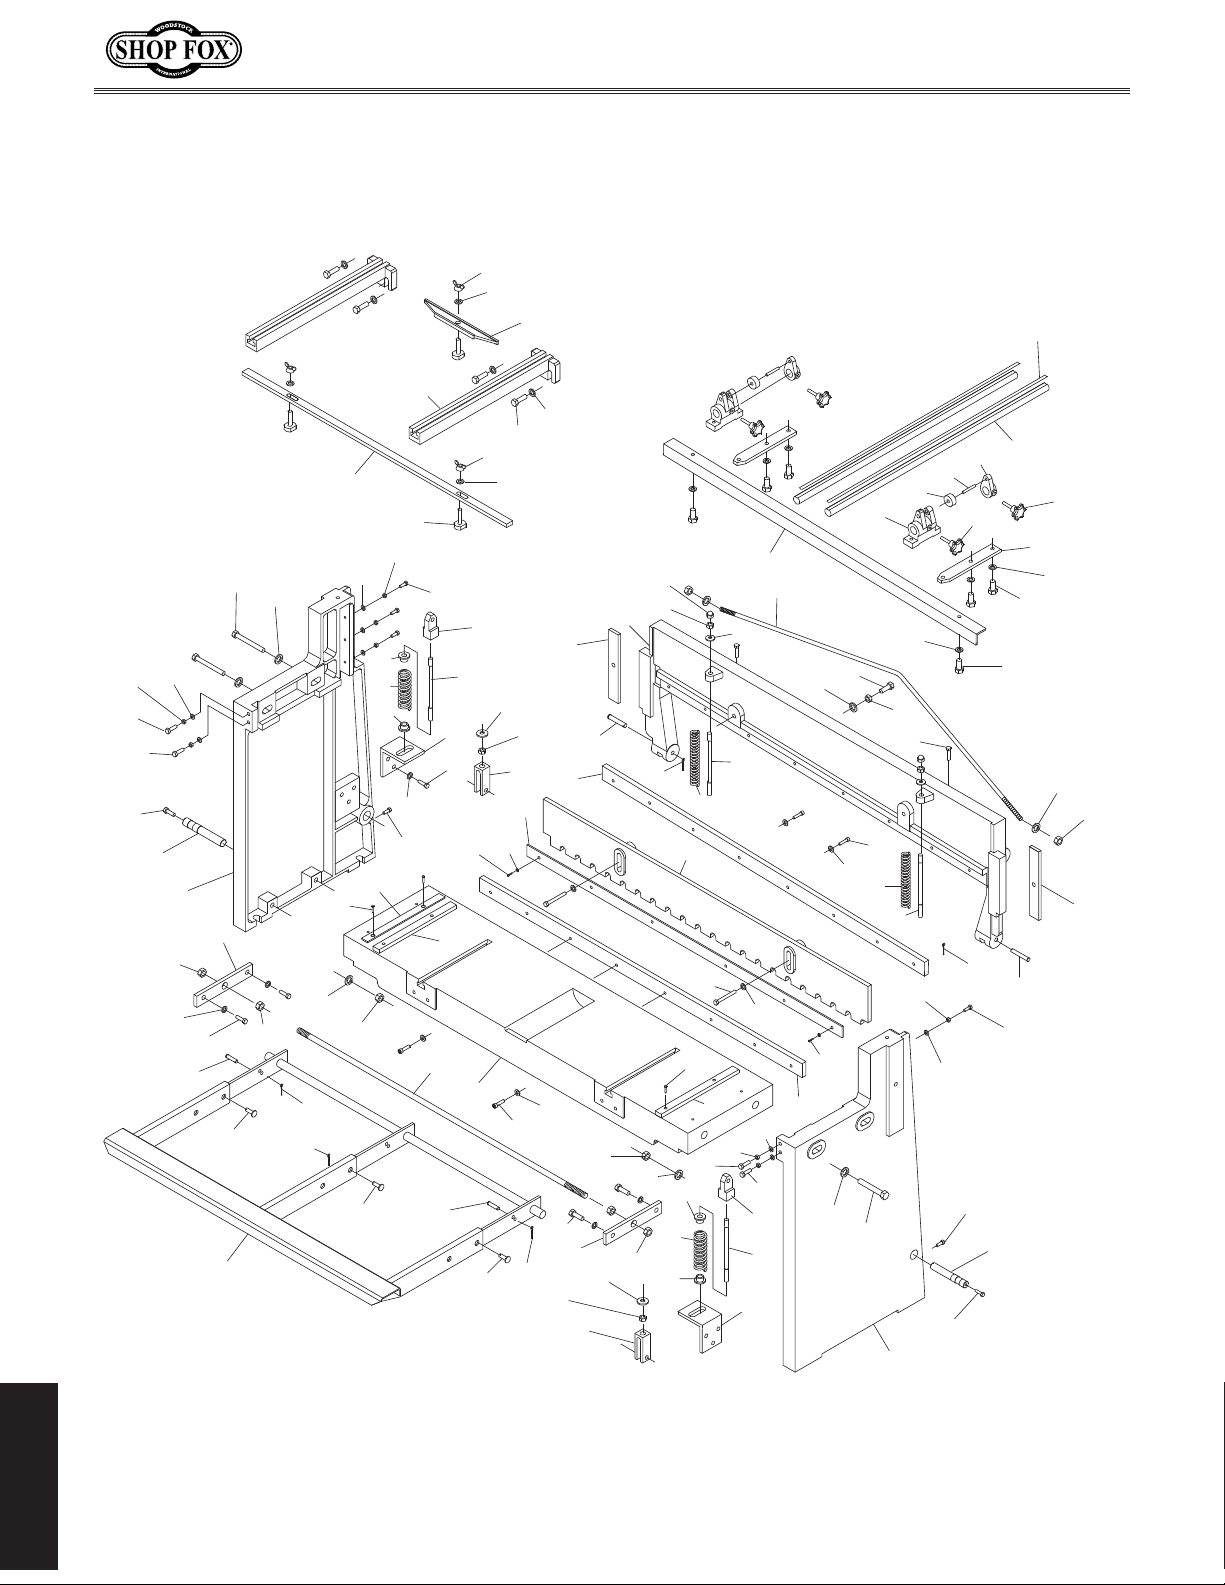
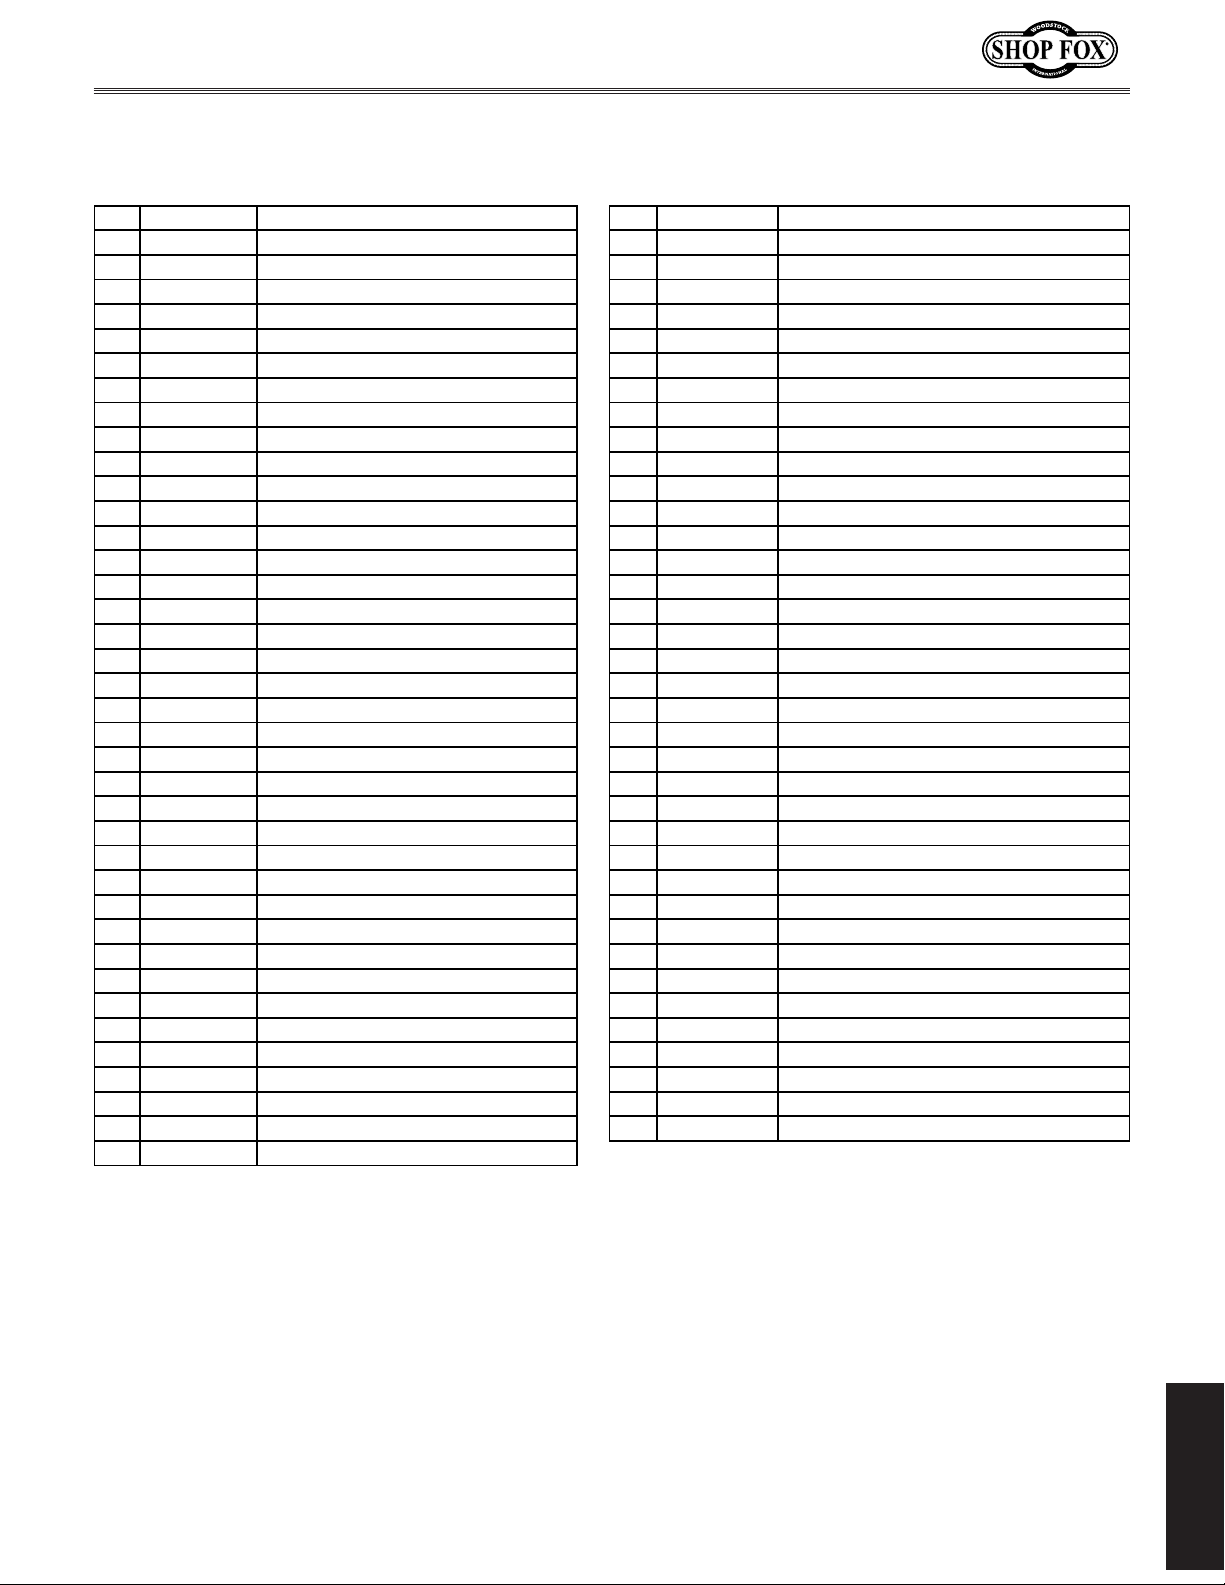
Main Parts List
REF PAR T # DESCRIPTION REF PAR T # DESCRIPTION
1 XM1117001 TABLE 41 XM1117041 COMPRESSION SPRING 8 X 46 X 275
2 XM1117002 CUTTER BAR 42 XM1117042 SPR ING CAP
3 XM1117003 HOLD DOWN 43 X M1117043 PIVOT BLOCK
4 XM1117004 SIDE PANEL (RIGHT) 44 XM1117044 P IVOT BRACK ET
5 XM1117005 SIDE PANEL (LEFT) 45 XM1117045 STUD-UDE M16-2 X 320, 2, 16
6 XM1117006 EXTENSION ARM 46 XM1117046 FLAT WASH ER 16MM
7 XM1117007 HEX BOLT M12-1.75 X 30 47 XM1117047 H EX NUT M16-2
8 XM1117008 COMPRESSIO N SPRING 3 X 22 X 165 48 XM1117048 SPR ING MOUNTING BRACKET
9 XM1117009 STUD-UDE M12-1.75 X 220, 25, 45 49 XM1117049 H EX BOLT M10-1.5 X 25
10 XM1117010 ACORN NUT M12-1.75 50 XM1117050 H EX NUT M16-2
11 XM1117011 H EX B OLT M12-1.75 X 80 51 X M1117051 CLEVIS PIN 12 X 88MM
12 XM1117012 FLAT WASH ER 12MM 52 X M1117052 CLEVIS PIN 12 X 45MM
13 XM1117013 BLADE GUARD 53 XM1117053 HINGE PIN
14 XM1117014 P HLP HD SCR M6-1 X 15 54 XM1117054 FOOT PEDAL ASSEMBLY
15 XM1117015 90- DEG STOP 55 X M1117055 STUD-DE M16-2 X 1480, 60
16 XM1117016 TABLE SCALE 56 X M1117056 CLEVIS PIN 20 X 36MM
17 XM1117017 H EX B OLT M8-1.25 X 25 57 XM1117057 H EX BOLT M12-1.75 X 25
18 XM1117018 H EX B OLT M10-1.5 X 60 58 XM1117058 H EX BOLT M10-1.5 X 25
19 XM1117019 H EX B OLT M10-1.5 X 50 59 XM1117059 REAR WORK STOP
20 XM1117020 FLAT WASH ER 10MM 60 X M1117060 REAR WORK STOP MOUNT
21 XM1117021 H EX B OLT M16-2 X 120 61 XM1117061 MICRO-ADJUSTMENT BLOCK
22 XM1117022 FLAT WASH ER 16MM 62 X M1117062 KNOB M10-1.5, D35, ROUND KD
23 XM1117023 H EX NUT M16-2 63 XM1117063 STUD-FT M10-1.5 X 90
24 XM1117024 UPPER BLADE 64 XM1117064 H EX BOLT M10-1.5 X 30
25 XM1117025 LOWER BLADE 65 XM1117065 KNOB BOLT M8-1. 25 X 25, 6-LOBE, D35
26 XM1117026 CAP SCREW M10-1. 5 X 45 66 XM1117066 REAR WORK STOP ADJUSTMENT BLOCK
27 XM1117027 CAP SCREW M10-1. 5 X 50 67 XM1117067 CONNECTING ST UD BRACKET
28 XM1117028 FLAT WASH ER 10MM 68 X M1117068 HEX BOLT M10-1.5 X 20
29 XM1117029 FLAT WASH ER 10MM 69 X M1117069 SUPPORT ROD
31 XM1117031 GIB 70 XM1117070 H EX NUT M16-2
32 XM1117032 CAP SCREW M10-1. 5 X 45 71 XM1117071 FRONT WORK STOP
33 XM1117033 H EX NUT M10-1.5 72 XM1117072 FLAT WASH ER 12MM
34 XM1117034 BLADE BOW ROD 73 XM1117073 T-BOLT M12-1.75 X 45
35 XM1117035 FLAT WASH ER 14MM 74 X M1117074 WING NUT M12-1.75
36 XM1117036 H EX NUT M14-2 75 XM1117075 BEVEL G AUGE
37 XM1117037 B OW BOLT M16-2 X 60 76 XM1117076 COTTER PIN M3 X 50 STANDARD
38 XM1117038 H EX NUT M12-1.75 77 XM1117077 FLAT WASHER 6MM
39 XM1117039 FLAT WASH ER 16MM 78 X M1117078 SUPPORT ROD SCALE
40 XM1117040 H EX B OLT M10-1.5 X 40
-35-
PARTS
Page 38
Model M1117 (For Machines Mfd. Since 9/21)
M1117
102
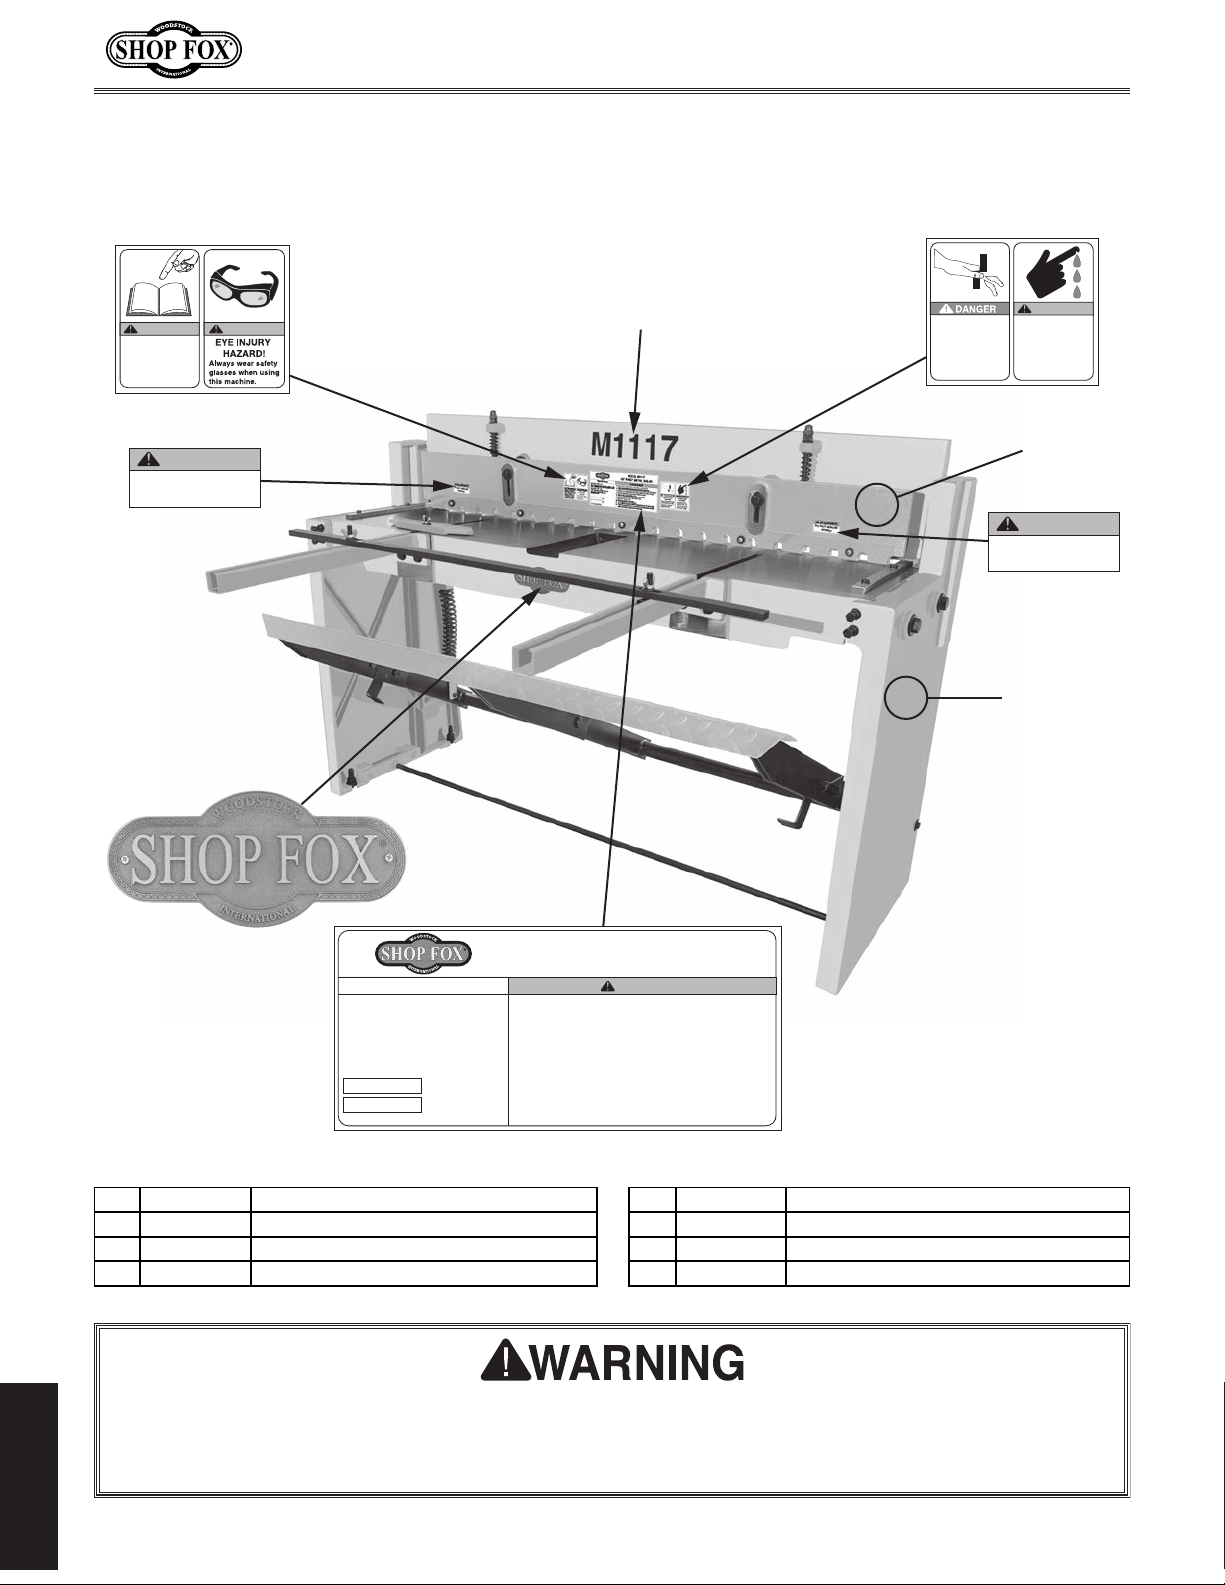
Labels & Cosmetics
101
WARNING! WARNING!
READ and UNDERSTAND
MANUAL to avoid serious
injury! If a manual is not
available, DO NOT use
machine! Instead, go to
www.woodstockint.com
or call (360) 734-3482.
105
WARNING!
DO NOT REMOVE
GUARD!
108
AMPUTATION
HAZARD!
Keep hands and fingers
out of blade path when
shearing or serious
injury will occur!
103
WARNING!
!
LACERATION
HAZARD!
Wear gloves while
handling metal and
chamfer and deburr
sharp metal edges.
104
105
WARNING!
DO NOT REMOVE
GUARD!
106
107
MODEL M1117
52" SHEET METAL SHEAR
Specifications
Max. Stock Width: 52"
Max. Thickness, Mild Steel, Half Width: 14 Ga.
Max. Thickness, Mild Steel, Full Width: 16 Ga.
Max. Beam Lift: 1-3/4"
Front Stop Scale Range: 0–12-1/2"
Rear Stop Scale Range: 0–33"
Weight: 982 lbs.
Date
Mfd. for Woodstock in China
S/N
To reduce risk of serious injury while using this machine:
1. Read and understand owner’s manual before operating.
2. Always wear ANSI-approved eye protection and heavy leather gloves.
3. Chamfer and deburr sharp metal edges before and after cutting.
4. Always keep guards in place and in working order.
5. Secure shear to floor before using.
6. Always keep hands and fingers away from blade.
7. Do not exceed rated capacity of this shear.
8. Do not cut wire or nails.
9. Rotate or sharpen dull blades.
10. Do not place foot under foot pedal.
11. Do not operate under influence of drugs or alcohol or when tired.
12. Prevent unauthorized use by children or untrained users; restrict
access or disable machine when unattended.
WARNING!
REF PAR T # DESCRIPTION REF PAR T # DESCRIPTION
101 X M1117101 MANUAL/EYE INJURY LABEL 105 XM1117105 DO NOT REMO VE GUARD LABEL
102 X M1117102 MODEL NUMBER LABEL 106 XM1117106 TOUCH-UP PAINT, SHOP FOX WHITE
103 X M1117103 AMPUTATION/LACERATION LABEL 107 XM1117107 MACHINE ID LAB EL
104 X M1117104 TOUCH - UP PAINT , CAUTION YELLO W 108 XM1117108 SHOP FOX NAMEPLATE SMALL
Safety labels warn about machine hazards and how to prevent serious personal injury. The owner
of this machine MUST maintain the original location and readability of all labels on this machine.
If any label is removed or becomes unreadable, REPLACE that label before allowing machine to
be operated again. Contact us at (360) 734-3482 or www.woodstockint.com to order new labels.
PARTS
-36-
Page 39
warranty does not apply to defects due directly or indirectly to misuse, abuse, negligence or accidents,
WARRANTY
WARRANTY
Woodstock International, Inc. warrants all Shop Fox machinery to be free of defects from workmanship
and materials for a period of two years from the date of original purchase by the original owner. This
lack of maintenance, or reimbursement of third party expenses incurred.
Woodstock International, Inc. will repair, replace, or arrange for a dealer refund, at its expense and
option, the Shop Fox machine or machine part proven to be defective for its designed and intended
use, provided that the original owner returns the product prepaid to an authorized warranty or repair
facility as designated by our Bellingham, Washington office with proof of their purchase of the product
within two years, and provides Woodstock International, Inc. reasonable opportunity to verify the
alleged defect through inspection. If it is determined there is no defect, or that the defect resulted
from causes not within the scope of Woodstock International Inc.'s warranty, then the original owner
must bear the cost of storing and returning the product.
This is Woodstock International, Inc.’s sole written warranty and any and all warranties that may be
implied by law, including any merchantability or fitness, for any particular purpose, are hereby limited
to the duration of this written warranty. We do not warrant that Shop Fox machinery complies with
the provisions of any law, acts or electrical codes. We do not reimburse for third party repairs. In no
event shall Woodstock International, Inc.’s liability under this limited warranty exceed the purchase
price paid for the product, and any legal actions brought against Woodstock International, Inc. shall be
tried in the State of Washington, County of Whatcom. We shall in no event be liable for death, injuries
to persons or property or for incidental, contingent, special or consequential damages arising from the
use of our products.
Every effort has been made to ensure that all Shop Fox machinery meets high quality and durability
standards. We are commited to continuously improving the quality of our products, and reserve the
right to change specifications at any time.
To register the warranty, go to https://www.woodstockint.com/warranty, or scan the QR code below.
You will be directed to the Warranty Registration page on www.woodstockint.com. Enter all applicable
production information.
WARRANTY
WOODSTOCKINT.COM
Page 40
 Loading...