

Page 1
INSTRUCTIONS FOR:
SUPERMIG
WELDERS
Supermig185.V2
Supermig195
Supermig220.V5
Supermig235.V4
MODEL No:
Original Language Version
SUPERMIG185.V2,195, 220.V5, 235.V4 Issue: 3 - 09/03/10
Page 2
1.2 IMPORTANT : THESE SUPERMIGS CAN BE CONNECTED TO EITHER A 30 AMP SINGLE PHASE SUPPLY OR A PROPERLY INSTALLED 13AMP
SUPPLY. TO ACHIEVE MAXIMUM OUTPUT HOWEVER A 30AMP FUSED SUPPLY SHOULD BE USED. WE RECOMMEND YOU DISCUSS THE
INSTALLATION OF AN INDUSTRIAL ROUND PIN PLUG & SOCKET WITH A QUALIFIED ELECTRICIAN.
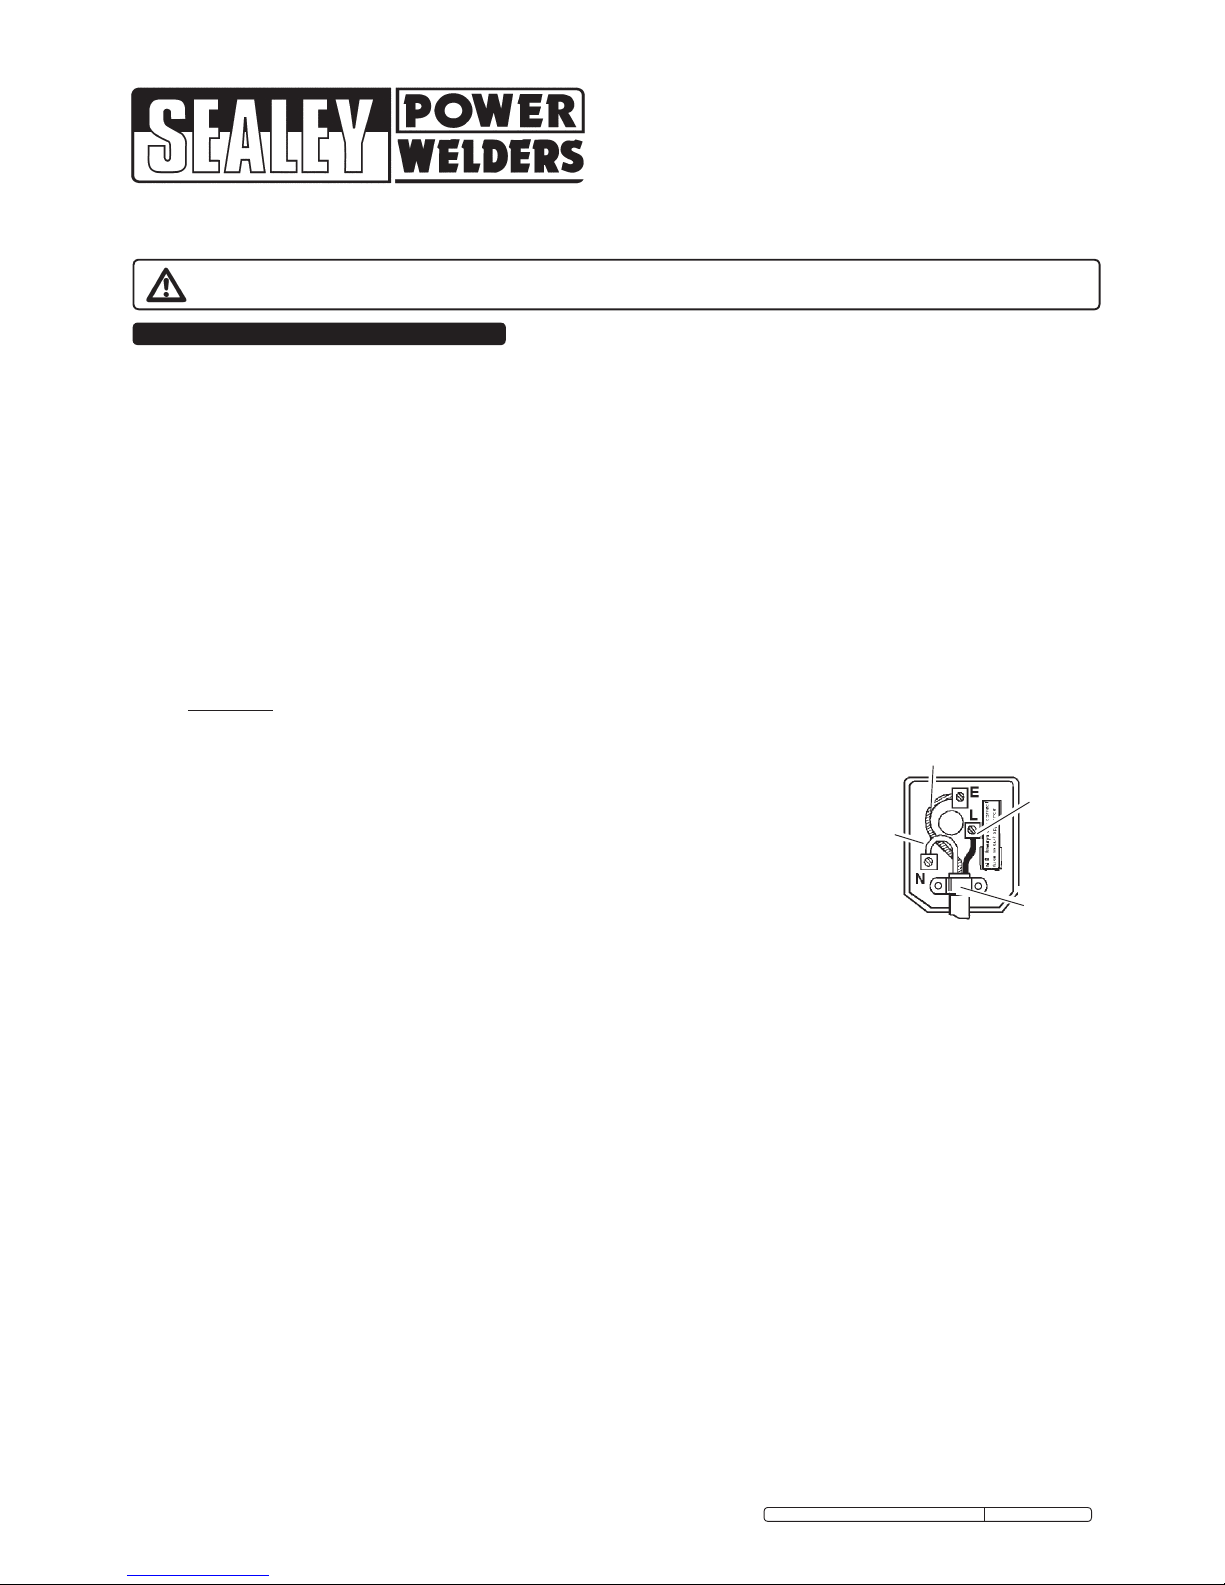
1.2.1. To fit a 13Amp plug proceed as follows: (UK only - see diagram on right).
Ensure the unit is correctly earthed via a three-pin plug.
a) Connect the GREEN/YELLOW earth wire to the earth terminal ‘E’.
b) Connect the BROWN live wire to live terminal ‘L’.
c) Connect the BLUE neutral wire to the neutral terminal ‘N’.
After wiring, check there are no bare wires, that all wires have been
correctly connected and that the wire restraint is tight.
1.2.2. Cable extension reels. When a cable extension reel is used it should be fully unwound before connection.
A cable reel with an RCD fitted is recommended since any product which is plugged into the cable reel will
be protected. The cross-section of the cable on the cable reel must be suitable for the unit and never lower
than the cross-section of the main cable supplied with unit.
FUSE RATING IS 13Amp.
INSTRUCTIONS FOR
MODELS:
Thank you for purchasing a Sealey Welder. Manufactured to a high standard this product will, if used according to these instructions and properly maintained, give
you years of trouble free performance.
SUPERMIG185.V2
SUPERMIG195
SUPERMIG220.V5
SUPERMIG235.V4
IMPORTANT: BEF OR E USING THIS PROD UC T, PLE ASE READ THE INS TRU CTI ON S CAREF UL LY. M AKE CAREF UL NOTE OF SAF ETY IN STR UCT ION S,
WARNINGS AND CAUTIONS. THIS PRODUCT SHOULD ONLY BE USED FOR ITS INTENDED PURPOSE. FAILURE TO DO SO MAY CAUSE DAMAGE
OR PERSONAL INJURY, AND WILL INVALIDATE THE WARRANTY. RETAIN THESE INSTRUCTIONS FOR FUTURE USE.
1. SAFETY INSTRUCTIONS
1.1. ELECTRICAL SAFETY. WARNING! It is the user’s responsibility to read, understand and comply with the following:
You must check all electrical equipment and appliances to ensure they are safe before using. You must inspect power supply leads, plugs and all electrical connections
for wear and damage. You must ensure the risk of electric shock is minimised by the installation of appropriate safety devices. An RCCB (Residual Current Circuit
Breaker) should be incorporated in the main distribution board. We also recommend that an RCD (Residual Current Device) is used with all electrical products. It is
particularly important to use an RCD together with portable products that are plugged into an electrical supply not protected by an RCCB. If in doubt consult a
professional electrician. You may obtain a Residual Current Device by contacting your Sealey dealer. You must also read and understand the following instructions
concerning electrical safety.
1.1.1. The Electricity At Work Act 1989 requires all portable electrical appliances, if used on business premises, to be tested by a qualified
Electrician at least once a year, using a Portable Appliance Tester (PAT).
1.1.2. The Health & Safety at Work Act 1974 makes owners of electrical appliances responsible for the safe condition of the appliance, and the safety of the
appliance operator. If in any doubt about electrical safety, contact a qualified electrician.
1.1.3. Ensure the insulation on all cables and the product itself is safe before connecting to the mains power supply. See 1.1.1. & 1.1.2. above and use a Portable
appliance Tester (PAT).
1.1.4. Ensure that cables are always protected against short circuit and overload.
1.1.5. Regularly inspect power supply, leads, plugs and all electrical connections for wear and damage, especially power
connections, to ensure that none are loose.
1.1.6. Important: Ensure the voltage marked on the product is the same as the electrical power supply to be used, and check tha plugs are fitted with the correct
capacity fuse.
1.1.7. DO NOT pull or carry the powered appliance by its power supply lead. Products such as welders must not be pulled or carried by their output cables.
1.1.8. DO NOT pull power plugs from sockets by the power cable.
1.3. GENERAL SAFETY
DANGER!: Unplug the welder from the mains power supply before performing maintenance or service.
Keep the welder and cables in good working order and condition. (Take immediate action to repair or replace damaged parts).
Use genuine parts and accessories only. (Non recommended parts may be dangerous and will invalidate the warranty).
Use an air hose to regularly blow out any dirt from the liner, and keep the welder clean for best and safest performance.
Check and spray the gas cup and contact tip regularly with anti-spatter spray available from your Sealey dealer.
Locate welder in a suitable working area for its function. Ensure area has adequate ventilation as welding fumes can be harmful.
Keep working area clean, tidy and free from unrelated materials. Also ensure the working area has adequate lighting, and that a fire extinguisher is at hand.
WARNING: Use welding head shield to protect eyes and avoid exposing skin to ultraviolet rays given off by electric arc. Wear safety welding
gauntlets.
Remove ill fitting clothing, remove ties, watches, rings, and other loose jewellery, and contain long hair.
Ensure the workpiece is correctly secured before operating the welder.
Avoid unintentional contact with workpiece. Accidental or uncontrolled use of the torch may be dangerous and will wear the nozzle.
Keep unauthorised persons away from the working area. Any persons working within the area must wear protective head shield and gloves.
Operators must receive adequate training before using the welder. The welder must only be operated under supervision.
Stand correctly keeping a good footing and balance, and ensure the floor is not slippery, and wear non-slip shoes.
Turn voltage switch to "0" (off) when not in use.
DO NOT operate the welder if it or its cables are damaged and DO NOT attempt to fit any non genuine torches, components, or parts to the welder unit.
DO NOT get welder wet or use in damp or wet locations or areas where there is condensation.
DANGER! DO NOT weld near flammable materials, solids, liquids, or gases, and DO NOT weld containers or pipes which have held flammable
materials or gases, liquids or solids. Avoid welding on ( or near to ) materials cleaned with chlorinated solvents.
DO NOT stand welder on a metal workbench, car bodywork or similar object.
DO NOT touch any live metal parts of the torch or electrode while the machine is switched on.
DO NOT pull the welder by the cable, or the torch. DO NOT bend or strain cables. Protect cables from sharp or abrasive items. DO NOT stand on cables
or leads. Protect cables from heat. Long lengths of slack cable must be gathered & neatly coiled. DO NOT place cables where they may endanger others.
DO NOT touch the torch or workpiece immediately after welding as they will be very hot. Allow to cool.
DO NOT operate welder while under the influence of drugs, alcohol or intoxicating medication, or if fatigued.
When not in use store the welder in a safe, dry, childproof area.
1.4. GAS SAFETY
Store gas cylinders in a vertical position only and ensure the storage area is correctly secured.
DO NOT store gas cylinders in areas where temperature exceeds 50°C. DO NOT use direct heat on a cylinder. Always keep gas cylinders cool.
DO NOT attempt to repair or modify any part of a gas cylinder or valve, and DO NOT puncture or damage a cylinder.
DO NOT obscure or remove any official labels from a cylinder. Always check the gas identity before use. Avoid getting gas cylinders oily or greasy.
DO NOT lift a cylinder by its cap, guard or valve. Always keep caps and guards in place and close valve when not in use.
Blue
Neutral
wire
Yellow & Green
Earth wire
Wire
restraint
Brown
Live
wire
Original Language Version
SUPERMIG185.V2,195, 220.V5, 235.V4 Issue: 3 - 09/03/10
Page 3
3. 1. Wheel Assembly
3. 1. 1. Turn machine upside down, and remove the screws attached to the bottom front. Use these screws to
attach the front castor wheels.
3. 1. 2. Take the rear axle and fit a wheel to one end by placing a washer, then the wheel, a second washer
and then insert a split pin.
3. 1. 3. Pass the axle through the two brackets under the gas cylinder carrier, then fit the other washer,
wheel, washer, split pin.
3. 2. Connecting the gas cylinder
3. 2. 1. When using Argon or Argon mixtures, use the Bull Nose Adaptor. If you intend to use CO2 gas, the
regulator will fit directly onto the cylinder. Fit the Bull Nose Adaptor to the cylinder with a spanner.
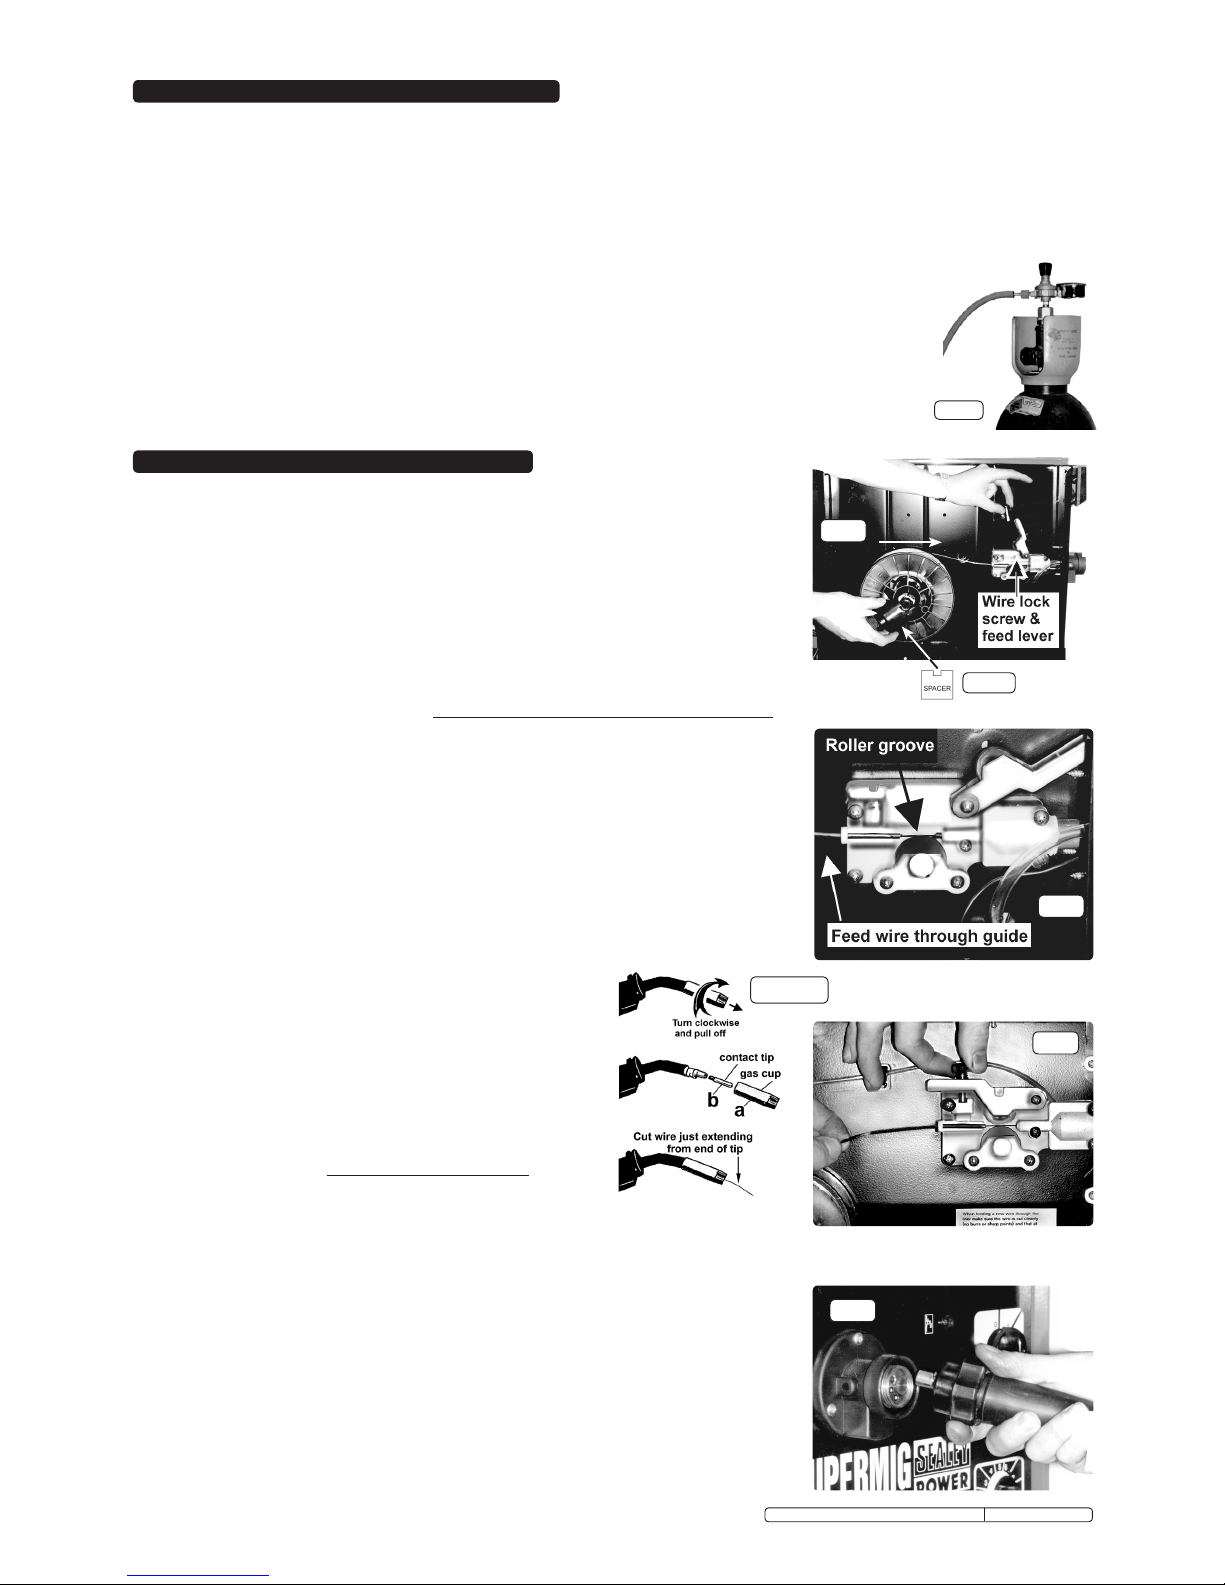
3. 2. 2. Fit the gas regulator on the Bull Nose Adaptor and connect it to the machine gas hose (fig.1).
3. 2. 3. Set the regulator flow rate to 5-8 litres/min depending on the material to be welded, and whether there
are draughts which are strong enough to disturb the gas flow.
3. 3. Mobile use of welder with gas cylinder attached. The welder should only be transported with a
small or medium gas cylinder attached. Do not transport the welder with a large cylinder attached.
3. 4. Fitting a reel of wire Wire capacity: (Mild Steel). 5 - 15 kilos. ( 5 kilos for 185 )
3. 4. 1. Push reel of wire over reel holder end springs and onto reel holder ensuring the spool rotates
clockwise, with the wire drawing off reel from the top (see white arrow in fig 2). Large spools of wire
have a guide hole which must be pushed onto plastic pin located at the end of the reel holder. This
pin will stop larger reels from free wheeling.
3. 4. 2. To secure the reel of wire take the plastic spacer and identify the two cut outs at one end (fig 2a).
Place the spacer over the holder end springs and onto the reel holder ensuring the two cut outs are
facing inward toward the reel of wire (fig. 2).
3. 4. 3. Undo the wire lock screw and lift the wire feed lever up to the right (fig 2).
3. 4. 4. Straighten about 40-50mm of spool wire (do not allow wire to uncoil), and gently push wire through
the plastic guide and through the 6 or 8mm roller groove (see 6.3), and through to the torch (fig. 3).
3. 4. 5. Carefully return the tension arm and secure wire with the wire lock screw.
3. 4. 6. Remove gas cup (fig 3.4.6.a) and contact tip (b) from end of torch as follows:
a) Take torch in left hand with the torch tip facing to the right.
b) Grasp gas cup firmly in your right hand.
c) Turn gas cup clockwise only (c) and pull cup out to the right.
WARNING! do not turn gas cup anti-clockwise, as this will
damage the internal spring.
d) Unscrew copper contact tip (right hand thread) to remove.
3. 4. 7. Check welder is switched off “0”, and that the earth clamp
is away from the torch tip. Connect the welder to the mains
power supply and set the voltage switch to one.
3. 4. 8. Set the wire speed knob to position 5 or 6. Keep the
torch cable as straight as possible and press the torch switch.
The wire will feed through the torch.
3. 4. 9. When the wire has fed through, switch welder off, unplug from mains.
a) Take torch in left hand and screw contact tip back into place.
b) Grasp gas cup in right hand, push onto torch head and
turn clockwise only. Do not turn gas cup anti-clockwise, as this will
damage the internal spring.
c) Cut wire so that it is just protruding from the cup.
3. 5. Setting wire tension. (fig 4).
IMPORTANT: You must set the correct tension. Too little or too much tension will cause problematic
wire feed and result in poor welding.
3. 5. 1. Tension between rollers is checked by slowing down the wire between your fingers. If top feed roller
skids the tension is correct. Use as low a tension as possible, too high a tension will disfigure wire
and result in a blown fuse.
3. 6. Clutch adjustment. Note: It is essential that the clutch is adjusted correctly.
3. 6. 1. Once the wire is fed through the torch, switch on the machine and set the wire speed to maximum.
3. 6. 2. Depress torch switch and release quickly. If the spool overruns it indicates that the clutch is too loose.
3. 6. 3. Tighten the clutch (located in the centre of the wire spool holder fig 2) with a screwdriver and test the
machine as above until the wire stops over running.
Note: DO NOT over tighten the clutch as this will cause wire feed problems and strain the motor.
3. 7. Euro Connection. Your welder has a Euro Torch Connection. Line up pins in the torch with the
appropriate holes in the machine, push in and tighten knurled knob (fig. 5). When welding is finished
remove torch and store in a safe place. Note: damage to torches and cables is not covered by
warranty.
3. ASSEMBLY & PREPARATION
A
fig 2
fig 2a
fig 4
fig 3
fig 5
Model No: ................... SUPERMIG185.V2 ................ SUPERMIG195 .............SUPERMIG220.V5 ............ SUPERMIG235.V4
Welding Current: .......................30-185A ...................... 30-195A ......................40-220A .....................35-235A
Wire Capacity steel: . . . . . . . . . . . . . . . . . . . . . . . . 5kg ....................... 5-15kg .......................5-15kg ...................... 5-15kg
Duty Cycle: . . . . . . . . . . . . . . . . . . . . 100% @60Amps ............... 100% @60Amps ...............100% @70Amps .............. 100% @80Amps
Cooling System: . . . . . . . . . . . . . . . . . . . . . .Forced Air .....................Forced Air ....................Forced Air ................... Forced Air
Gas Type: . . . . . . . . . . . . . . . CO2/Argon mix & Argon ..........CO2/Argon mix & Argon .........CO2/Argon mix & Argon ........ CO2/Argon mix & Argon
Torch: . . . . . . . . . . . . . . . . . . . . . . . . . . Euro Non Live ................. Euro Non Live .................Euro Non Live ................ Euro Non Live
Absorbed power . . . . . . . . . . . . . . . . 230V 1ph 5.2kW ............... 230V 1ph 5.2kW ...............230V 1ph 6.0kW .............. 230V 1ph 7.0kW
2. SPECIFICATIONS & INTRODUCTION
IMPORTANT: These instructions contain information you require to prepare your machine for welding, together with a maintenance and
trouble shooting section. If you have no previous experience the instructions are not intended to show you how to become a welder .
Should you have no experience, we recommend that you seek training from an expert source. Mig welding is relatively easy to perform,
but does require a steady hand and time practising under supervision with scrap metal as it is only with continued practice that you will
achieve the desired results.
INTRODUCTION: These Supermigs are compact power sources, that operate on a forced air cooling system to slow transformer heating
in order to increase the duty cycle. They also have a non live torch to prevent the risk of accidentally striking an arc. Your Supermig is
designed to operate with two diameters of welding wire: 0.6mm, & 0.8mm. The 185 will accommodate a 5kgs wire spool, whilst the 195,
220 & 235 will accommodate 5 to 15kgs wire spools. All Models are equipped with: Torch, Mini reel of 0.6mm wire, Regulator,
Gas hose.
fig 3.4.6.
fig 1
Original Language Version
SUPERMIG185.V2,195, 220.V5, 235.V4 Issue: 3 - 09/03/10
Page 4
A spool of welding wire is positioned on the welder ’s spool holder and automatically fed through an insulated liner in the torch to the
tip.The torch assembly consists of a switch, liner, gas hose, and control cable. The switch activates the wire feed roller and the gas
flow. Conversely, releasing the switch stops the wire feed and gas flow. The weld current is transferred to the electrode (the wire) from
the contact tip at the end of the torch. A gas cup fits over the contact tip to direct the gas flow towards the weld ensuring that the arc
welding process is shielded from oxidising air contaminates. The shielding gas also assists heating of the weld materials.
The torch is connected to the positive side of a DC rectifier, and the negative clamp is attached to the workpiece.
4. 1. PREPARATION FOR WELDING
IMPORTANT: BEFORE YOU COMMENCE, MAKE SURE THE MACHINE IS SWITCHED OFF AT THE MAINS. IF WELDING A CAR,
DISCONNECT THE BATTERY OR FIT AN ELECTRONIC CIRCUIT PROTECTOR. WE STRONGLY RECOMMEND THE USE OF
SEALEY “PROSAF/12V OR 24V IN ORDER TO PROTECT SOPHISTICATED ELECTRONICS. ENSURE YOU HAVE READ &
UNDERSTOOD THE ELECTRICAL SAFETY INSTRUCTIONS IN CHAPTER 1.
4.1.1. Connecting the Earth Lead
To ensure a complete circuit, the earth lead must be securely attached to the work piece that is to be welded.
a) Best connection is obtained by grinding clean the point of contact on the workpiece before connecting the earth clamp.
b) The weld area must also be free of paint, rust, grease, etc.
c) When welding a vehicle, be sure the vehicle battery is disconnected or fit an Electronic Circuit Protector available from
your Sealey dealer.
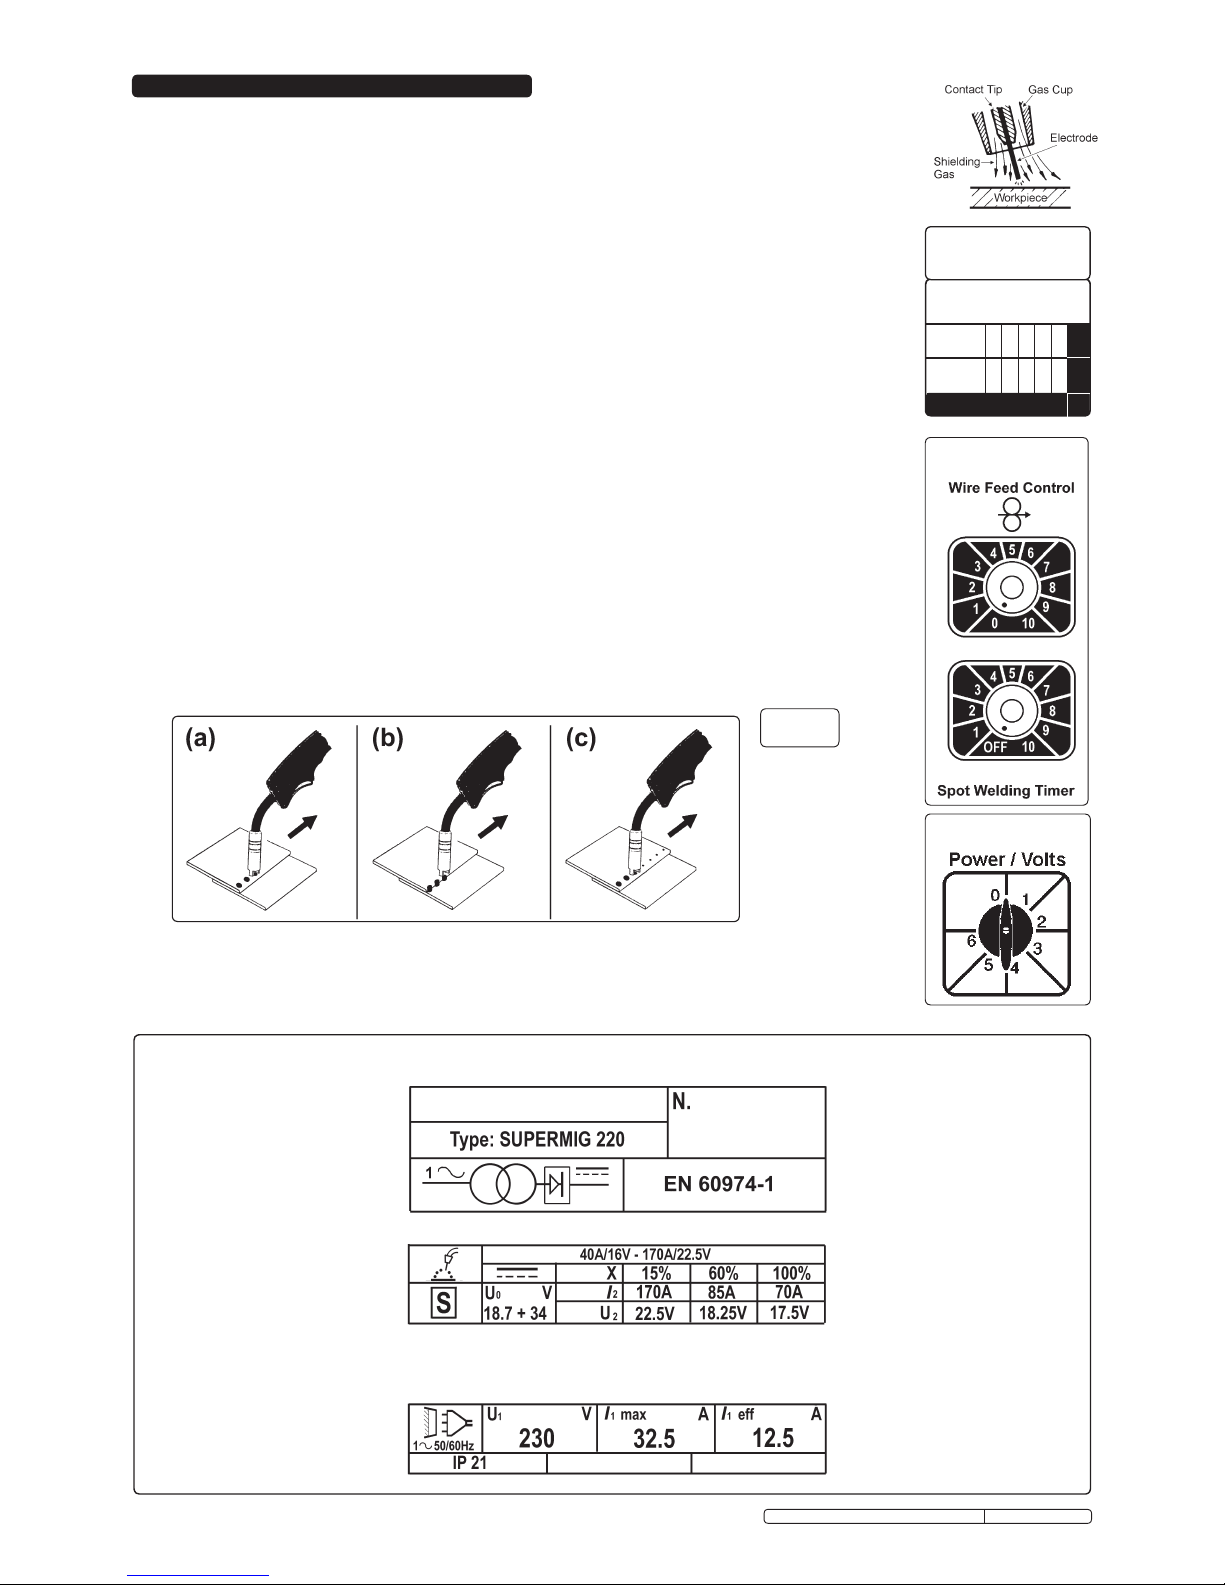
4.1.2. Power switch (fig B). Set the switch to position 1 or 2 for welding up to 2mm thickness.Use settings 3,4,5,6. for thicker welds.
4.1.3. Setting the welder controls. (fig A) In principle, the lower the amperage required, the slower the wire speed. See setting
chart for voltage and corresponding wire speeds.
Note: these settings a re only a guide and will vary according to the operators experience.
4. MIG/MAG WELDING
Wire 0.6mm Steel
Argon / CO2 Mix
Voltage
Step:
1 2 3 4 5 6
Wire
Speed:
5 6 7 8 9 10
SETTINGS SHOWN
AS GUIDE ONLY
fig. A
fig. B
Spot Welding Timer
6
6
10
Made in European Community
Position for Serial Number
British Standard number
Power output range shown as minimum
and maximum welding current and the
corresponding conventional load voltages.
Duty Cycle (X)
Rated weld current (I2)
Conventional load voltage (U2)
GUIDE TO RATINGS PLATE AND SYMBOLS ( For actual ratings of your model refer to front panel.
For further clarification refer to British Standard EN 60974-1 )
Direct current symbol
Welder model type
MIG/MAG welding symbol
Single Phase Transformer
and Rectifier (or 3 phase)
Indicates a welding power source
suitable for supplying power to welding
operations carried out in an environment
with increased hazard of electric shock.
International standard relating
to moisture ingress.
Indicates an alternating current
power supply and 1 or 3 phases as
required by specification.
4.1.4. Welding mild steel
To weld mild steel you can use CO2 gas for most tasks where spatter and the high build up of weld do not pose a problem.
( Welding with a long arc reduces penetration and widens the arc. This in turn results in more spatter. A long welding arc
can be appropriate for welding butt joints in thin materials. Welding with a short arc (at the same weld settings) results in
greater penetration and a narrower weld and reduces the amount of spatter.)
To achieve a consistent spatter free and flat weld, you must use an Argon/CO2 mixture.
4.1.5. To weld aluminium use: Argon gas, 0.8mm Contact Tip (AK957), 0.8mm Aluminium Wire, (MIG/2/KAL08).
4.1.6. Spot Welding. Spot welding may be carried out as shown in fig.C below.
It will be necessary to fit a spot welding gas cup. ( Sealey part No. 120/722150 )
(a) Overlapping metal sheets with a maximum thickness of 0.8 mm may be welded as indicated.
(b) Alternatively they may be welded edge to surface as indicated.
(c) For thicker sheet pre drilled holes holes may be employed.
4.1.7. Use the wire feed control in conjunction with the spot weld timer below it. To activate the timer turn the knob clockwise. The
settings indicated in the black portion of the chart are for guidance only and may vary with operators experience.
IMPORTANT.
Should you have no
welding experience, we
recommend you seek
training from an expert
source to ensure your
personal health & safety.
Good Mig welding may be
achieved only with
continued, supervised
practice.
4.1.8 OVERLOAD PROTECTION. Thermostatic overload protection is provided. When an overload has occurred, leave the unit
to cool. The thermostat will automatically reset the unit when the temperature has returned within limits
fig.C
Rated no-load voltage: (a) Peak value in case of direct current
(b) Peak and r.m.s. value in case of alternating current
Maximum effective supply current
Rated Supply Voltage
Rated maximum supply current
Original Language Version
SUPERMIG185.V2,195, 220.V5, 235.V4 Issue: 3 - 09/03/10
Page 5
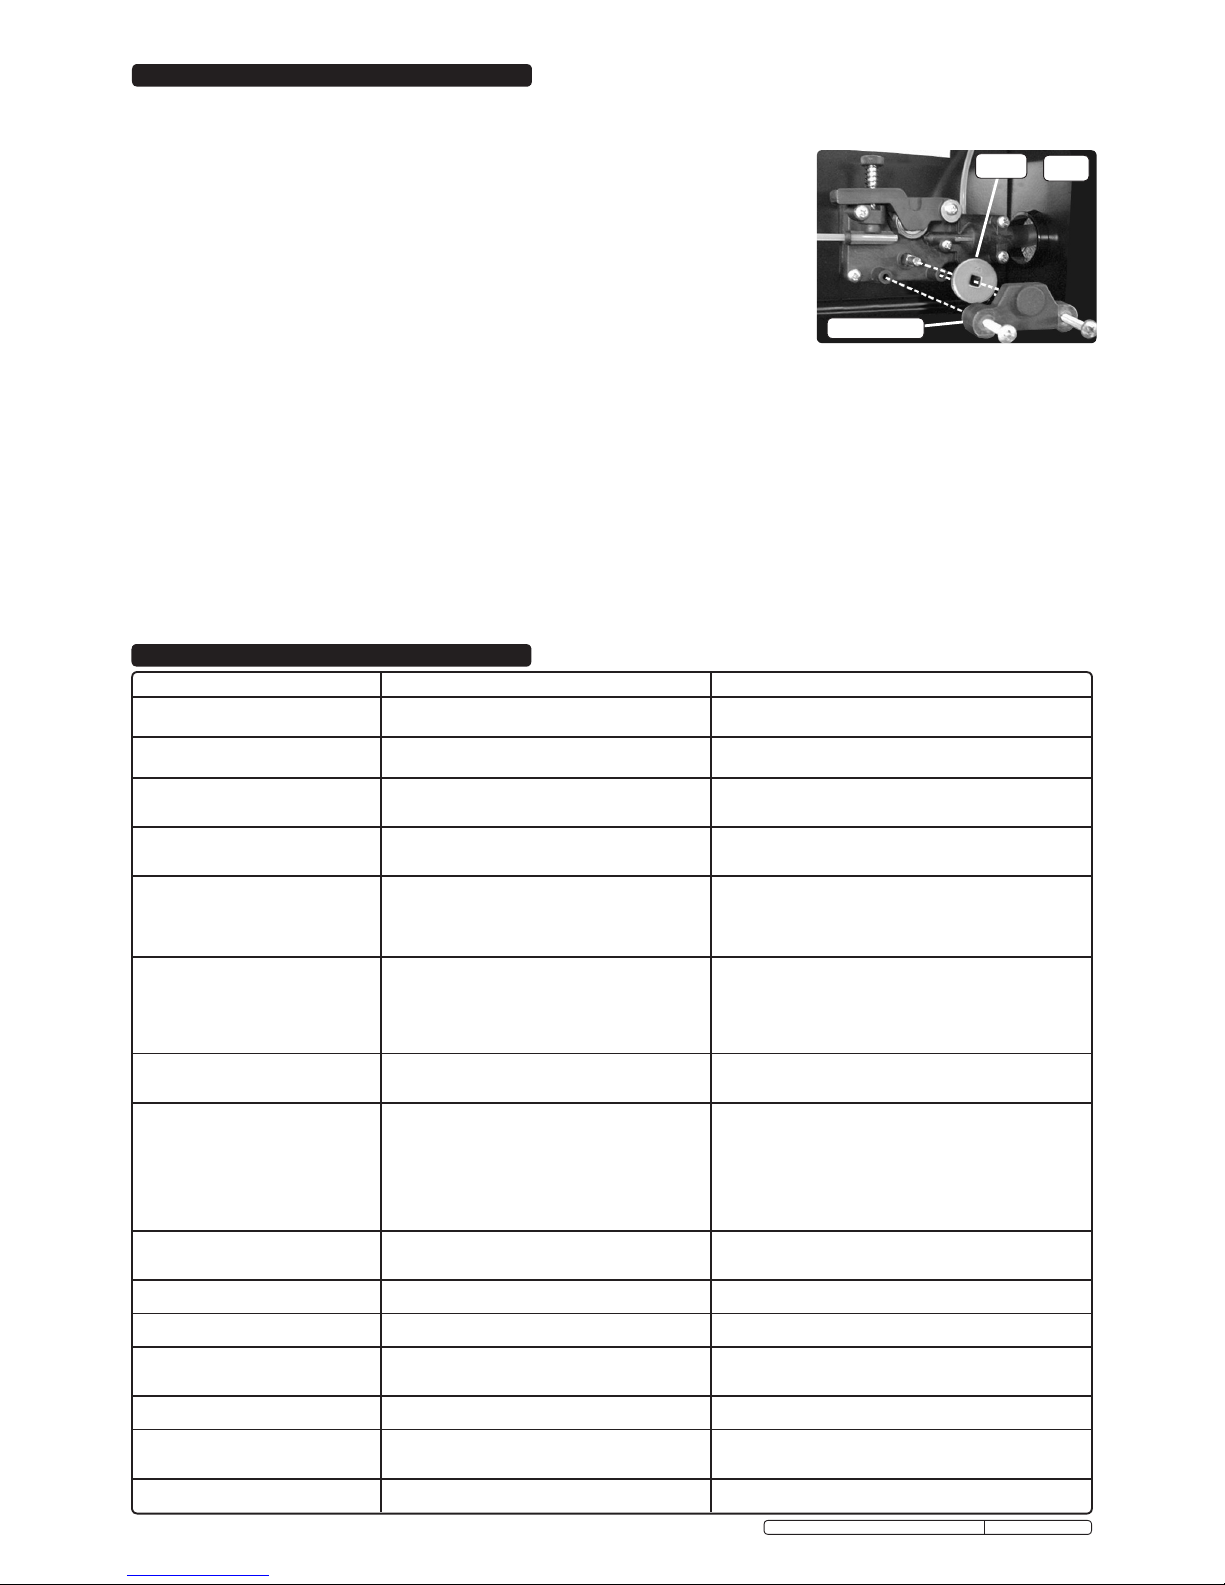
5.1. Wire feed unit
Check the wire feed unit at regular intervals. The feed roller wire guide plays an important part in obtaining consistent results. Poor wire
feed affects welding. Clean the rollers weekly, especially the feed roller groove, removing all dust deposits.
5.2. Torch
Protect the torch cable assembly from mechanical wear. Clean the liner from the machine
forwards by using compressed air. If the liner is clogged it must be replaced.
5.3. Changing Feed Roller
( IMPORTANT: Adjust the feed roller to the corresponding wire size.) There are two grooves
on the feed roller, 0.6mm and 0.8mm. Always use the groove on the outside of the roller, (the
groove nearest to you). To remove the feed roller, undo the two screws and remove the plastic
cover (fig 6). Clean and turn, or if damaged change the feed roller and replace the plastic
cover accordingly.
5.4. Contact Tip (to remove tip follow steps in 3.3.6 to replace 3.3.9 a & b very carefully).
The contact tip is a consumable item and must be replaced when the hole becomes
enlarged or oval. The contact tip MUST be kept free from spatter to ensure an unimpeded flow of gas.
5.5. Gas Cup (to remove cup follow steps in 3.3.6. and to replace 3.3.9. a & b very carefully).
The gas cup must also be kept clean and free from spatter. Build up of spatter inside the gas cup can cause a short circuit at the
contact tip which will result in either the fuse blowing on the printed circuit card, or expensive machine repairs. To keep the contact tip
free from spatter, we recommend the use of Sealey anti-spatter spray (MIG/722307) available from your Sealey Dealer.
5.6. Replacing the Liner
Wind the wire back on to the spool and secure it. Unscrew the torch from the machine and undo the brass nut. The liner should now
be visible. Pull it out and replace with a new one.
5.7. Changing gears
An inexperienced welder can allow spatter to build up in the tip and shroud. In severe cases this can block the feed causing gear
stripping in the drive motor. To check if the gears are worn depress the button on the torch with the set switched on. If the gears are
worn, a grating sound will be heard coming from the wire feed motor, you may also observe the feed roller vibrating instead of rotating.
Should this be the case, open the gearbox, remove the worn or damaged gears and replace with new ones.
5.8. Changing Fuses
The fuse is located on the auxiliary transformer and is mainly blown for the following reasons:
Spatter collecting in the gas cup, causing contact tip to short circuit. Wire tension is too great. A sudden surge of current.
5. MAINTENANCE
6 . TROUBLESHOOTING
Roller
Plastic cover
fig 6
PROBLEM POSSIBLE CAUSE SOLUTION
1. Power source stops Overheating protection activated due to overload Protection automatically resets when transformer has cooled
(about 15mins)
2. No weld current, fuse blowing
in 13 amp plug
Rectier blown Replace rectier
3. No weld current Bad conncection current between clmp and wprkpeice
Break in earth lead
Brek in torch lead
Clean or grind contact surface and weld area
Repair or replace earth lead
Repair or replace torch
4. Feed motor not working, lamp
is on
Fuse blown
Gear damage or worn
Motor defective
Replace fuse 1.5amp (Chapter 5)
Replace gears (Chapter 5)
Replace motor (contact service agent)
5. Wire does not feed, feed roller
rotates
Pressure roller improperly adjusted
Dirt, copper, duct, etc, has collected in torch liner
Gas cup (nozzle) or tip defective
Deformed wire
Adjust tension
Clean the liner from the machine forward. Use compressed air.
If too much dirt, replace the liner. (Chapter 5)
Replace gas cup (nozzle) and/or tip. (Chapter 5)
Check roller tension and adjust it necessary (Chapter 3)
6. Wire feeds unevenly Dirt, etc, in wire
Gas cup (nozzle) or tip defective
Gas cup (nozzle) spattered
Feed roller groove clogged
Feed roller grove deformed
Pressure roller tension improper
Clean the liner from the machine forward. Use compressed air.
Replace gas cup (nozzle) and/or tip. (Chapter 5)
Clean or replace gas cup (nozzle) (Chapter 5)
Clean feed roller. (Chapter 5)
Replace feed roller (Chapter 5)
Adjust tension (Chapter 3)
7. Unstable arc Incorrect setting
Impurities in weld area
Worn or defective gas cup (nozzle)
Check settings. (Chapter 4)
Clean and/or grind workpiece. (Chapter 4)
Replace gas cup (nozzle). (Chapter 5)
8. Porous weld No gas
Gas cup clogged
Draft blowing away shielding gas
Rusty or dirty joints
Torch too far from or at wrong angle to work
Gas leak
Faulty Electrovalve
Open gas cylinder, regulate gas ow
Clean or replace cup. (Chapter 5)
Screen off welding site or increase gas ow
Clean or grind the workpeice. (Chapter 4)
The distance from gas cup to workpeice should be 8-10mm
Check hoses, connections and torch assembly. (Chapter 6)
Press the gas cup in correct position
Clean out or replace
9. Electrode sticking in gas cup (nozzle) Worn or defective gas cup (nozzle)
Electrode deformed
Wire speed too slow
Replace gas cup (nozzle). (Chapter 5)
Check roller tension. (Chapter 3)
See recommendation for wire speed
10. Irregular weld head Torch incorrectly held
Wire weaving in weld pool
Use correct torch angle
Check roller tension and adjust as needed. (Chapter 3)
11. Weld bead too narrow and
raised
Weld current too low
Weld speed too high
Increase power and wire speed. (Chapter 4)
Move torch slower and weave a little more
12. Weld bead too wide Weld current too high
Weld speed too low
Arc too long
Decrease power and wire speed. (Chapter 4)
Move torch faster and weave less
Bring torch closer to workpiece
13. Poor penetration Weld current too low
Arc too long
Increase power and wire speed. (Chapter 4)
Bring torch closer to workpiece
14. Excessive penetration Weld current too high
Weld speed too slow
Incorrect distance of torch too workpiece
Decrease power and wire speed. (Chapter 4)
Move torch faster
Torch distance should be 8-10mm
15. Fuse blowing Tension too great
Gas cup contract tip clogged
Releace tension. (Chapter 3)
Clean gas cup and contact tip. (Chapter 5)
Original Language Version
SUPERMIG185.V2,195, 220.V5, 235.V4 Issue: 3 - 09/03/10
Page 6
Supermig185.V2
Supermig195
Supermig220.V5
Supermig235.V4
MODEL No's:
NOTE: It is our policy to continually improve products and as such we reserve the right to alter data, specifications and component parts without prior notice.
IMPORTANT: No liability is accepted for incorrect use of this product.
WARRANTY: Guarantee is 12 months from purchase date, proof of which will be required for any claim.
INFORMATION: For a copy of our latest catalogue and promotions call us on 01284 757525 and leave your full name and address, including postcode.
01284 757500
01284 703534
Sole UK Distributor, Sealey Group,
Kempson Way, Suffolk Business Park,
Bury St. Edmunds, Suffolk,
IP32 7AR
www.sealey.co.uk
Web
email
Original Language Version
SUPERMIG185.V2,195, 220.V5, 235.V4 Issue: 3 - 09/03/10
 Loading...