

Page 1
INSTRUCTIONS
SUPERMIG 250/10
Thank you for purchasing a Sealey product. Manufactured to a high standard this product will, if used according to these instructions
and properly maintained, give you years of trouble free performance.
01284 757500 01284 703534
E-mail [email protected]
SUPERMIG250-Job181-280198
2. INTRODUCTION & DESCRIPTION
These instructions are to assist you prepare your mig set for welding together with information on maintenance, and trouble shooting. Read this
manual carefully in order to get the best results from your welding set. The instructions are not intended to show you how to be an expert welder.
It is with continued practice that you will achieve the desired results. Mig welding requires a steady hand, time spent practising with scrap metal
will gain rewards when you progress to an actual workpiece.
Supermig 250/10 is a compact power source fitted with a heavy duty wire feed motor. The wire feed system itself is automatic thus providing
the best possible opportunity to achieve the most effective weld. The machine operates on a forced air cooling system to slow the transformer
heating in order to increase the duty cycle, and a non live torch to prevent the risk of accidentally striking an arc.
IMPORTANT: BEFORE USING THIS PRODUCT, PLEASE READ THE INSTRUCTIONS CAREFULLY. MAKE CAREFUL NOTE OF SAFETY iNSTRUCTIONS,
WARNINGS AND CAUTIONS. THIS PRODUCT SHOULD ONLY BE USED FOR ITS INTENDED PURPOSE. FAILURE TO DO SO MAY CAUSE DAMAGE
OR PERSONAL INJURY, AND WILL INVALIDATE THE WARRANTY.
1. SAFETY INSTRUCTIONS
1.1 ELECTRICAL SAFETY. WARNING! It is the users responsibility to check the following:
You must check all electrical equipment and appliances to ensure they are safe before using. You must inspect power supply leads, plugs and all electrical
connections for wear and damage. You must ensure the risk of electric shock is minimised by the installation of appropriate safety devices. An RCCB (Residual
Current Circuit Breaker) should be incorporated in the main distribution board. W
e recommend that an RCD (Residual Current Device) is used with all electrical
products. It is particularly important to use an RCD together with portable products that are plugged into an electrical supply not protected by an RCCB. If in doubt
consult a professional electrician. Y
ou may obtain a Residual Current Device by contacting your Sealey dealer. You must also read and understand the following
instructions concerning electrical safety.
1.1.1. The Electricity At Work Act 1989 requires all portable electrical appliances, if used on a business premises, to be tested
by a qualified person at least once a year by using a Portable Appliance Tester (PAT).
1.1.2. The Health & Safety at Work Act 1974 makes owners of electrical appliances responsible for the safe condition of the appliance,
and the safety of the appliance operator. If in any doubt about electrical safety, contact a qualified electrician.
1.1.3. Ensure the insulation on all cables and product itself is safe before connecting to mains power supply. See 1.1.2. use a (PAT).
1.1.4. Ensure that cables are always protected against short circuit and overload.
1.1.5. Regularly check power supply, leads, plugs and all electrical connections for wear or damage, especially power connections
to ensure none are loose.
1.1.6. Check the voltage marked on the product is the same as the electrical power supply to be used. Check fused plugs
are fitted with correct capacity fuse.
1.1.7. DO NOT pull or carry the powered appliance by its power supply lead. Products such as welders
must not be pulled or carried by their output cables.
1.1.8. DO NOT pull power plugs from sockets by the power cable.
1.1.9. DO NOT use worn or damage leads, plugs or connections. Immediately replace or repair
by qualified persons. A U.K. 3 pin plug with ASTA/BS approval is fitted. In case of damage,
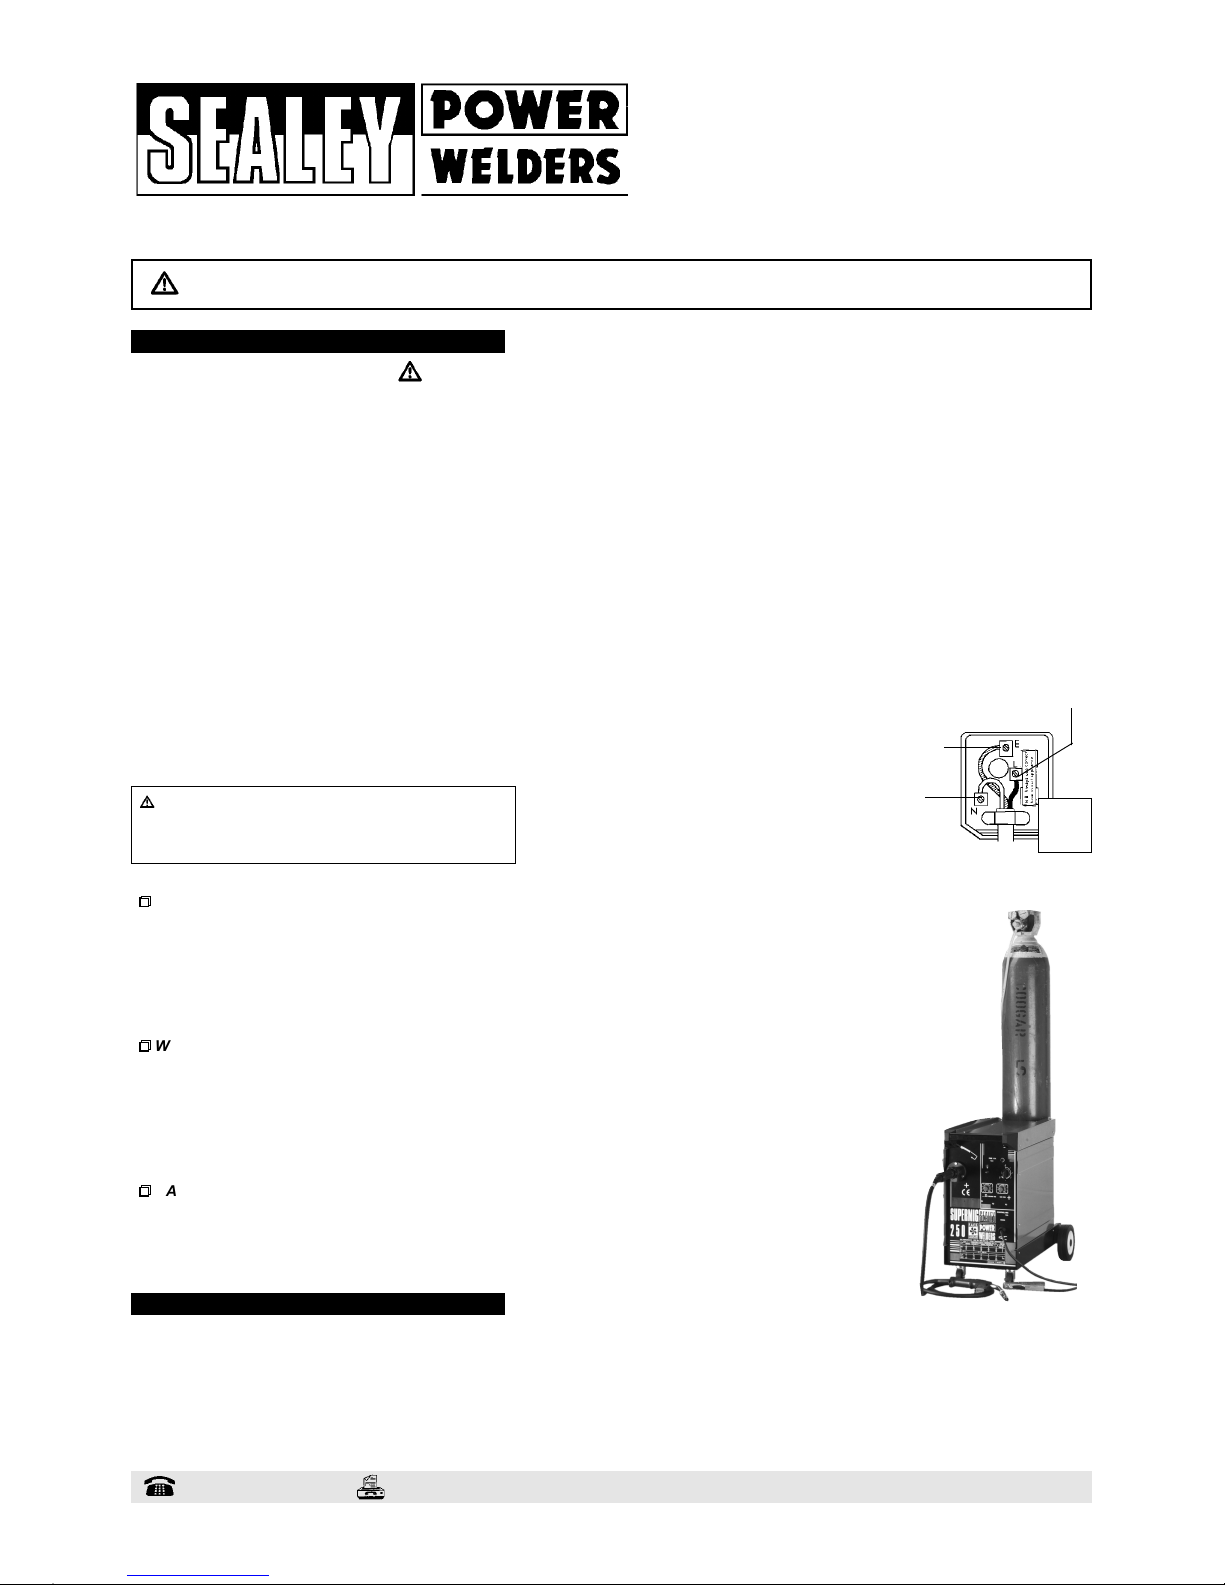
cut off and fit a new plug according to the following instructions (UK only - see diagram at right).
1.2 GENERAL SAFETY
p
p
p
WARNING: unplug the welder from the mains power supply before performing maintenance or service.
3Keep the welder and cables in good working order and condition. Take immediate action to repair or replace damaged parts.
3Use recommended parts and accessories only. Non recommended parts may be dangerous and will invalidate the warranty.
3Check the gas cup and contact tip, and spray regularly with anti-spatter spray available from your Sealey dealer.
Note: to remove gas cup ready instruction part 3.3.6. carefully.
3Use an air hose to regularly blow out any dirt from the liner, and keep the welder clean for best and safest performance.
3Locate the welder in an adequate working area for its function, and ensure the area is well ventilated.
3Keep working area clean and tidy and free from unrelated materials. Also ensure the working area has adequate lighting.
p
p
p
WARNING: use welding head shield to protect your eyes against ultraviolet rays, and safety welding gauntlets.
3Keep children and unauthorised persons away from the working area.
3T
urn voltage switch to "0" (off) when not in use.
3Stand correctly keeping a good footing and balance, and ensure the floor is not slippery.
3Remove ill fitting clothing, remove ties, watches, rings, and other loose jewellery, and contain long hair.
7DO NOT store gas cylinders in areas where temperature exceeds 50°C.
7DO NOT puncture or damage the gas cylinder.
7DO NOT use the welder in damp or wet locations.
p
p
p
DANGER! DO NOT weld near inflammable materials, solids, liquids, or gases.
7DO NOT operate welder while under the influence of drugs, alcohol or intoxicating medication, or if fatigued.
7DO NOT operate the welder if it or its cables are damaged.
7DO NOT allow untrained persons to operate the welder
.
7DO NOT pull the welder by the cable, or the torch, and DO NOT bend the torch.
Blue
Neutral
wire
Yellow
& Green
Earth wire
Brown Live wire
13 amp
3 pin
plug
a) Ensure the unit is correctly earthed via a three-pin plug.
b) Connect the Green/Yellow earth wire to the earth terminal E.
c) Connect the Brown live wire to live terminal L.
d) Connect the Blue neutral wire to the neutral terminal N.
WARNING! If you use the machine constantly at its higher power
settings, the welder must be plugged into a 30amp fused power
supply. If you are unsure if there is a 30amp supply at your premises,
contact a qualified electrician before proceeding further. (For the use
of a normal 13amp supply follow plug fitting instructions.
Page 2
To fit mains power plug see chapter 1. Note: you will need a 30amp electrical supply for higher power 0.8mm & 1.0mm settings.
3. 1. Wheel Assembly
3. 1. 1.
Turn the machine upside down.
3. 1. 2.
Remove the screws attached to the bottom front of the machine and use them to attach the front castor wheels.
3. 1. 3. Fit the large rear wheels to the rear axle with the split pins provided.
NOTE: be sure the wheel washers are fitted between the wheels on the axle.
3. 1. 4. Mount the complete axle assembly on to the rear of the welder body.
3.2. Connecting the gas cylinder
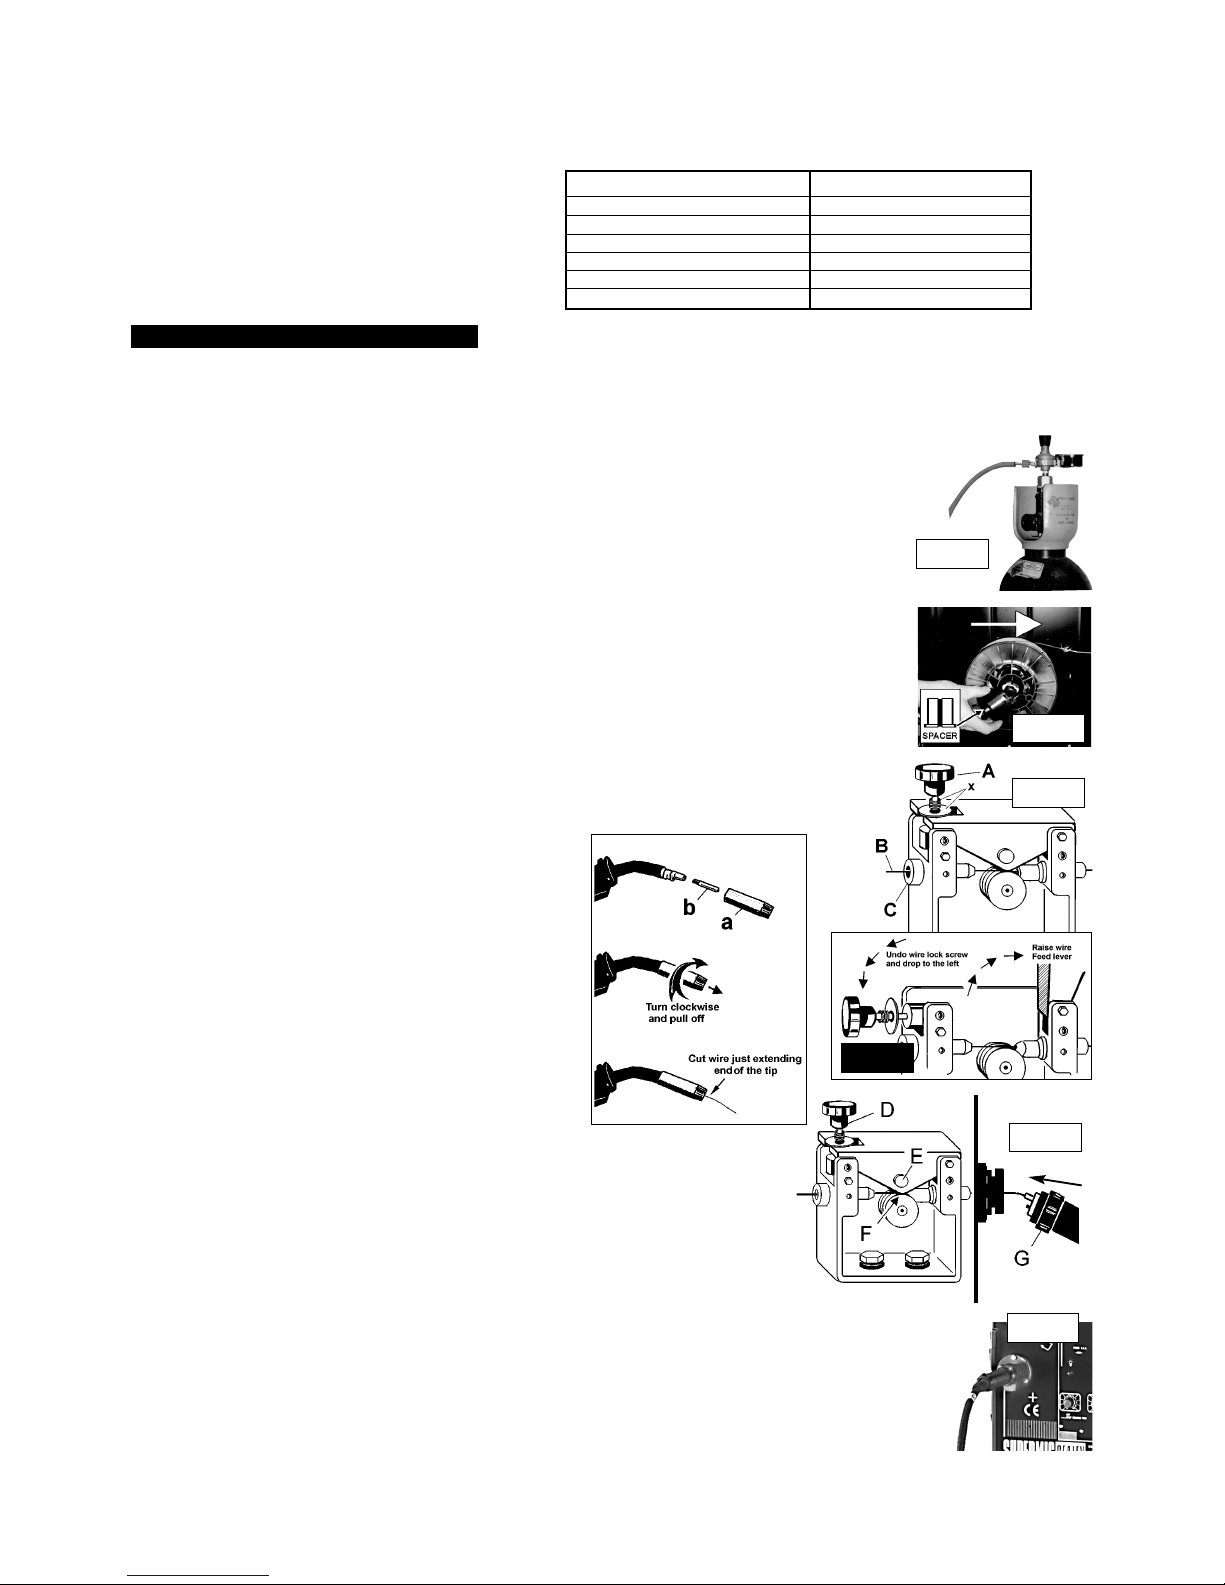
3. 2. 1. When using Argon or Argon mixtures you will need to use the bull nose adaptor. If you intend to use CO2 gas the
regulator will fit directly onto the cylinder.
3. 2. 2. Screw the bull nose adaptor to the cylinder with a spanner.
3. 2. 3.
Fit the gas regulator on to the bull nose adaptor and connect it to the machine gas hose (fig.1).
3. 2. 4. Set the regulator flow rate to 5-8 litres/min depending on the material to be welded, and whether there are draughts
which are strong enough to disturb the gas flow.
3. 3. Fitting a reel of wire
Wire capacity: (Mild Steel).......5 to 15 kilos.
3. 3. 1. Push the reel of wire over the reel holder end spring and onto the reel holder ensuring the spool rotates clockwise,
with the wire drawing off the reel from the top (see white arrow in fig 2). Large spools of wire have a guide hole which
must be pushed onto the plastic pin located at the end of the reel holder. This pin will stop larger reels from free
wheeling around the holder.
3. 3. 2. To secure the reel of wire take the plastic spacer and gently open the diameter of the spacer whilst placing over
the reel holder end spring and onto the reel holder (fig 2).
3. 3. 3. Undo the wire lock screw (fig 3 A) and slide to left, and raise the wire feed lever to the right (fig 4).
3. 3. 4. Straighten about 40-50mm of wire and gently push the wire through the brass guide (fig 3. B & C) into and through
the correct size feed roller groove, and on through the second brass guide into the torch.
3. 3. 5. Lower wire feed lever and clamp with the wire lock screw. Ensure the screw spring and washer are between
the head of the screw and the top of the feed lever (fig 3 x).
3. 3. 6. Remove gas cup (fig 3.3.6. a) and contact tip (b) from end of torch as follows:
a) Take torch in left hand with the torch tip facing to the right.
b) Grasp gas cup firmly in your right hand.
c) Turn gas cup clockwise only (c) and pull cup out to the right.
p WARNING! do not turn gas cup anti-clockwise, as this will
damage the internal spring.
d) Unscrew the copper contact tip (right hand thread) to remove.
3. 3. 7. Check welder is switched off 0, and that the earth clamp
is away from the torch tip. Connect the welder to the mains
power supply and set the voltage switch to one.
3. 3. 8. Set the wire speed knob to position 5 or 6. Keeping the torch
cable as straight as possible and press the torch switch.
The wire will feed through the torch.
3. 3. 9. When wire has fed through, switch welder off, unplug from mains.
a) Take torch in left hand and screw contact tip back into place.
b) Grasp gas cup in right hand, push onto torch head and
turn clockwise only.
p WARNING! do not turn gas cup anti-clockwise, as this will
damage the internal spring.
c) Cut wire so that it is just protruding the cup.
3. 4. Setting wire tension
It is important to set the correct tension (fig 5 F), too little or too much tension will cause problematic
wire feed and result in poor welding.
3. 4. 1. For 0.6mm wire in mild steel the wire lock screw should be tightened fully and then undone
approximately two turns (fig. 5 D).
3. 4. 2. Correct tension between the rollers is checked by slowing down the wire between the fingers.
If the top feed roller (fig 5 E) skids the tension is correct. T
ry to use as low a tension as possible,
for too high a tension will deform the wire and may result in a blown fuse.
3. 5. Clutch adjustment
It is essential that the clutch is adjusted correctly.
3. 5. 1. Once the wire is fed through the torch, switch on the machine and set the wire speed to maximum.
3. 5. 2. Depress torch switch and release quickly. If the spool overruns it indicates that the clutch is too loose.
3. 5. 3. Tighten the clutch (located in the centre of the wire spool holder) with a socket spanner and test the machine as above
until the wire stops over running.
NOTE: DO NOT OVER TIGHTEN THE CLUTCH AS THIS WILL CAUSE WIRE FEED PROBLEMS.
3. 6. Euro Connection
This welder is fitted with a Euro Connection quick release torch. (fig 6).
3. 6. 1. Simply line the pins in the torch up to the appropriate holes in the machine, push in and tighten with the knurled knob
(fig 5 G). Remember to remove the Torch after welding is completed and store in a safe dry place.
Note: Accidental damage to your torch is not covered by the guarantee.
3. ASSEMBLY
Fig 1.
MODEL 250/10 IS EQUIPPED WITH: 30.8mm Torch, 3Mini reel of 0.8mm wire, 30.8/1.0mm feed roller 3Regulator, 3Gas hose.
To weld with 0.6mm wire, order a reel of 0.6mm wire, and 0.6mm feed roller. To weld with 1.0mm wire, order a reel of 1.0mm wire
(The 250/10 is designed to accommodate 15kgs capacity 0.8mm & 1.0mm wire).
Your Supermig is designed to operate with three diameters of welding wire: 0.6mm, 0.8mm & 1.0mm wire, and will accommodate
a capacity range of 5 to 15Kgs.
Model Number SUPERMIG 210/10
Welding Current 35-250 Amps
Duty Cycle 100% @ 60A
50% @ 120A
20% @ 195A
15% @ 230A
Power efficiency 6.5 Kva
Welding
Capability
Chart:
SUPERMIG 250/10 - Job181 -280198
Fig 2.
Fig 3.
Fig 5.
Fig 6.
Fig 4.
Fig 3.3.6.
c
Page 3
Rated on-load voltage Uoin V
a) Peak value in case of direct current;
b) Peak & r
.m.s. value in case of alternating current.
Direct current
Fuse
X Duty cycle (Factor)
1
2
Rated weld current
U
2
Conventional load voltage
Mains supply and number of phases
(i.e. 1 or 3) with symbol for
alternating current.
(1)3
5. VARIOUS WELDING METHODS
4. MIG/MAG WELDING
Principles
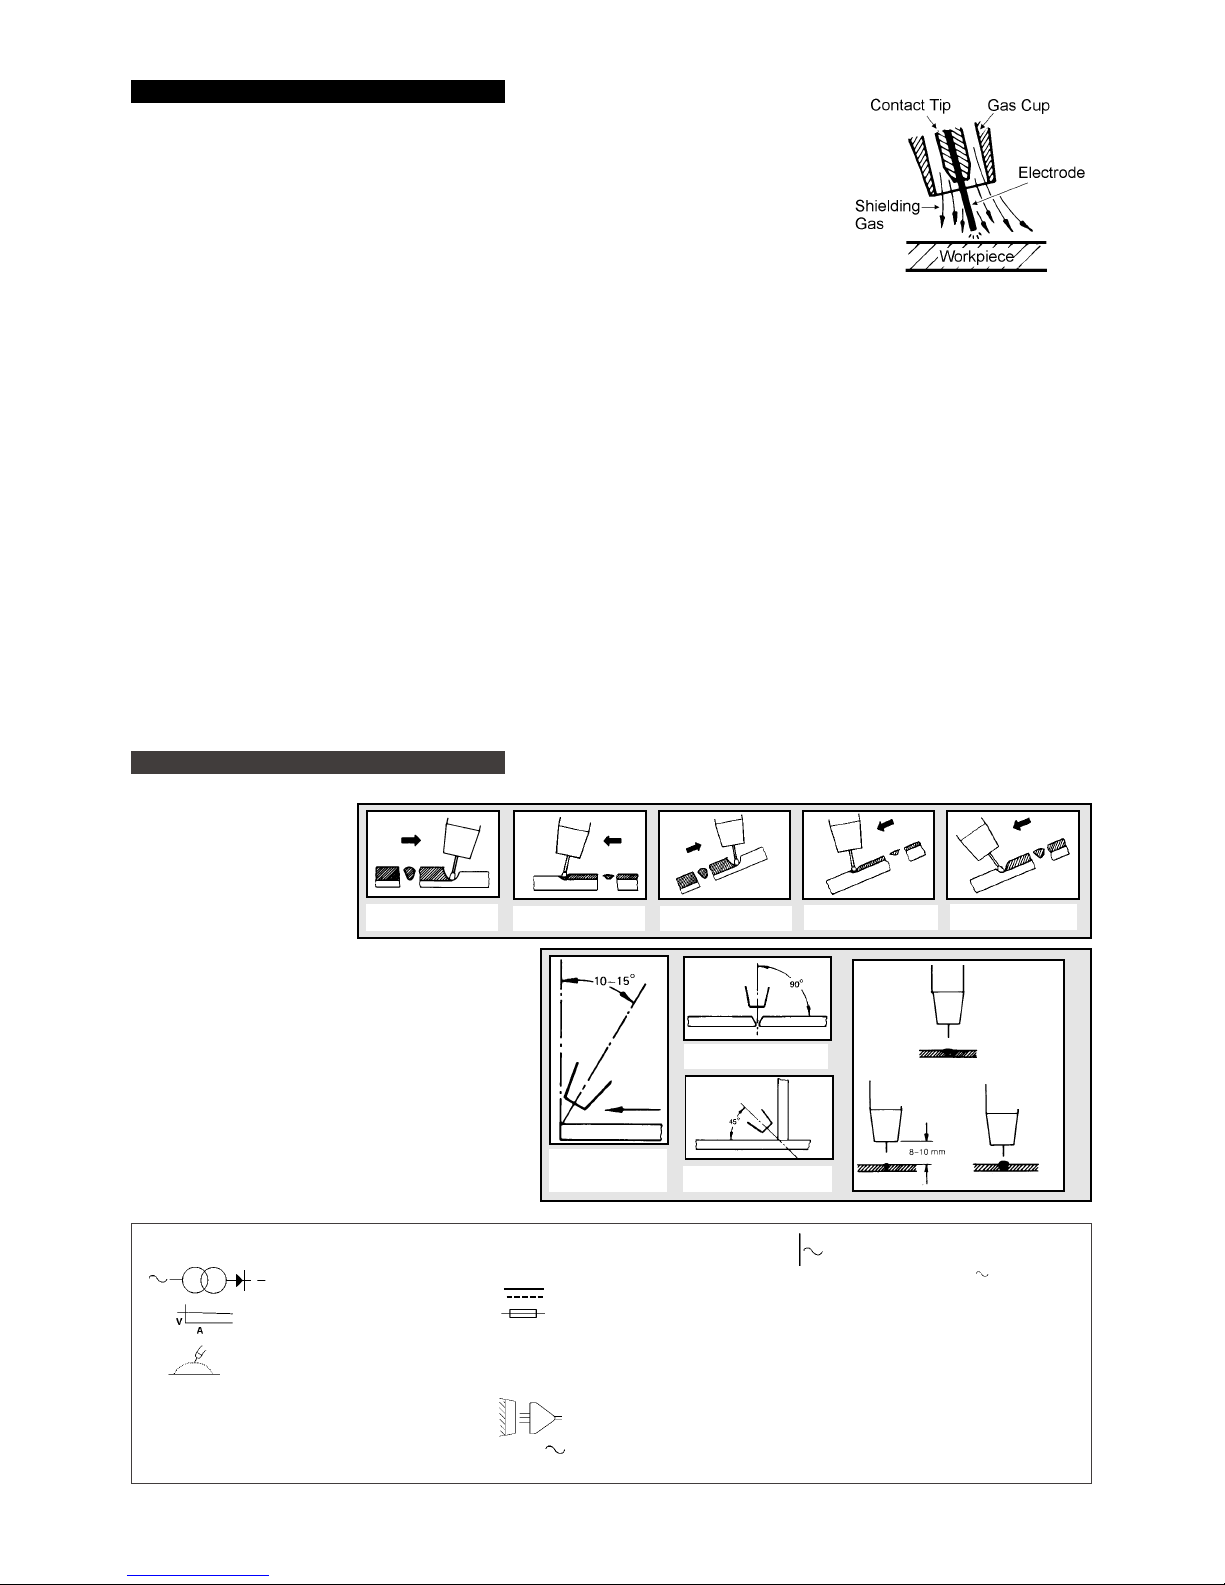
A spool of welding wire is positioned on the welders spool holder and automatically fed through
an insulated liner in the torch to the tip. The torch assembly consist of a switch, liner, gas hose,
and control cable. The switch activates the wire feed roller and the gas flow. Conversely, releasing
the switch stops the wire feed and gas flow. The weld current is transferred to the electrode (the wire)
from the contact tip at the end of the torch. A gas cup fits over the contact tip to direct the gas flow
towards the weld ensuring that the arc welding process is shielded from oxidising air contaminates.
The shielding gas also assists heating of the weld materials. The torch is connected to the positive
side of a DC rectifier, and the negative clamp is attached to the workpiece.
Preparation for welding.
IMPORT
ANT: Welder must be switched off at the mains before starting. If welding a vehicle, disconnect battery or fit an electronic circuit protector.
4.1. Connecting the Earth Lead
To ensure a complete circuit, the earth lead must be securely attached to the work piece that is to be welded.
4.1.1. The best connection is obtained by grinding clean the point of contact on the workpiece before connecting the earth clamp
to the job to be welded.
4.1.2. The weld area must also be free of paint, rust, grease, etc.
4.1.3. When welding a vehicle, be sure the vehicle battery is disconnected or fit a PROSAF/12V or 24V Electronic Circuit Protector
available from your Sealey dealer.
4.2. Setting Up
The Supermig250/10 has an automatic wire speed system, which for most effective welding should be set up as follows:
4.2.1. Select the voltage step that best suits the thickness of the material to be welded
4.2.2. Adjust the wire feed knob until a perfect weld bead is obtained.
NOTE: If the wire speed increases, even to reaching maximum, do not be concerned as the wire speed setting will re-adjust
correctly to any voltage step selected thereafter.
4.3. Welding mild steel
To weld mild steel you can use CO2 gas for most tasks where spatter and the high build up of weld do not pose a problem.
To achieve a spatter free and flat weld, you must use an Argon/CO2 mixture.
4.4. Welding aluminium
To weld aluminium use: 3 Argon gas, 3 0.8mm Contact Tip (AK957), 30.8mm Aluminium Wire, (MIG/2/KAL08).
Alternating current & the rated
frequency in hertz i.e. 50Hz
P
max
... kW
Maximum power consumption in case
of a rotating welding power source. This
value will only be given when it is not
combined with a prime mover.
U1... V/...Hz
Rated values of the supply voltage
and the frequency
.
/
1
Rated supply current.
IP Degree of protection, i.e. 21 or 23.
ED%
Duty cycle
%
The position of the torch,
its angle and direction of travel
in relation to the workpiece
is essential for the appearance
and quality of the weld.
The illustrations demonstrate
various positions and directions.
Rightward Welding
Welding in general
W
elding with a long arc reduces penetration and widens
the arc.
This in turn results in more spatter
.
A long welding arc can be appropriate for welding butt
joints in thin materials.
Welding with a short arc (at the same weld settings)
results in greater penetration and a narrower weld
and reduces the amount of spatter.
Leftward Welding
Vertical Rightward
Downhard leftward
Down Rightward
1. Direction of
Welding
3. Fillet Weld
3. Butt Weld
Normal
Welding
Arc
Long
Welding
Arc
Short
W
elding
Arc
MEANINGS OF MARKINGS, AND SYMBOLS
Single Phase transformer & rectifier
Flat Characteristic
MIG/MAG welding
...A/ ... V to ...A/ ... V Range of output, rated min
& max welding current and
their corresponding conventional
load voltage.
PA kVA Power Efficiency
SUPERMIG 250-Job181-280198
Page 4
6. 1. Wire feed unit
Check the wire feed unit at regular intervals. The feed roller wire guide plays an important part in obtaining consistent results. Poor wire
feeding affects welding. Clean the rollers weekly especially the feed roller groove removing all dust deposits.
6. 2. Torch
Protect the torch cable assembly from mechanical wear. Clean the liner from the machine forwards by using compressed air. If the liner
is clogged it must be replaced.
6. 3. Contact Tip (to remove tip follow steps in 3.3.6. and to replace 3.3.9. a & b very carefully).
The contact tip is a consumable item and must be replaced when the hole becomes enlarged or oval. The contact tip MUST be kept free from
spatter to ensure an unimpeded flow of gas.
6. 4. Gas Cup (or nozzle). (to remove cup follow steps in 3.3.6. and to replace 3.3.9. a & b very carefully).
The gas cup must also be kept clean and free from spatter. Build up of spatter inside the gas cup can cause a short circuit at the contact tip
which will result in either the fuse blowing on the printed circuit card, or expensive machine repairs. To keep the contact tip free from spatter
we recommend the use of Sealey anti-spatter spray (MIG/722307) available from your Sealey Dealer.
6. 5. Replacing the Liner
Wind the wire back on to the spool and secure it. Unscrew the torch from the machine and undo the brass nut. The liner should now be
visible. Pull it out and replace with a new one.
6. 6. Changing Fuses (The fuse is located on the circuit board).
A fuse is mainly blown for the following reasons:
3 Spatter collecting in the gas cup causing contact tip to short circuit. 3 Wire tension is too great. 3 A sudden surge of current.
6. 7. Changing Feed Roller
IMPORTANT: if necessary adjust the feed roller to the corresponding wire size by turning the roller around.
There are two grooves on the feed roller, 0.6mm and 0.8mm. Always use the groove on the outside of the roller, (the groove nearest to you).
To remove the feed roller, undo the hex nut and remove. Clean and turn, or if damaged change the feed roller.
6. 8. Electrical Safety
For full compliance with current legislation electrical integrity checks must the undertaken by a qualified competent person. See chapter 1
electrical safety.
6. MAINTENANCE
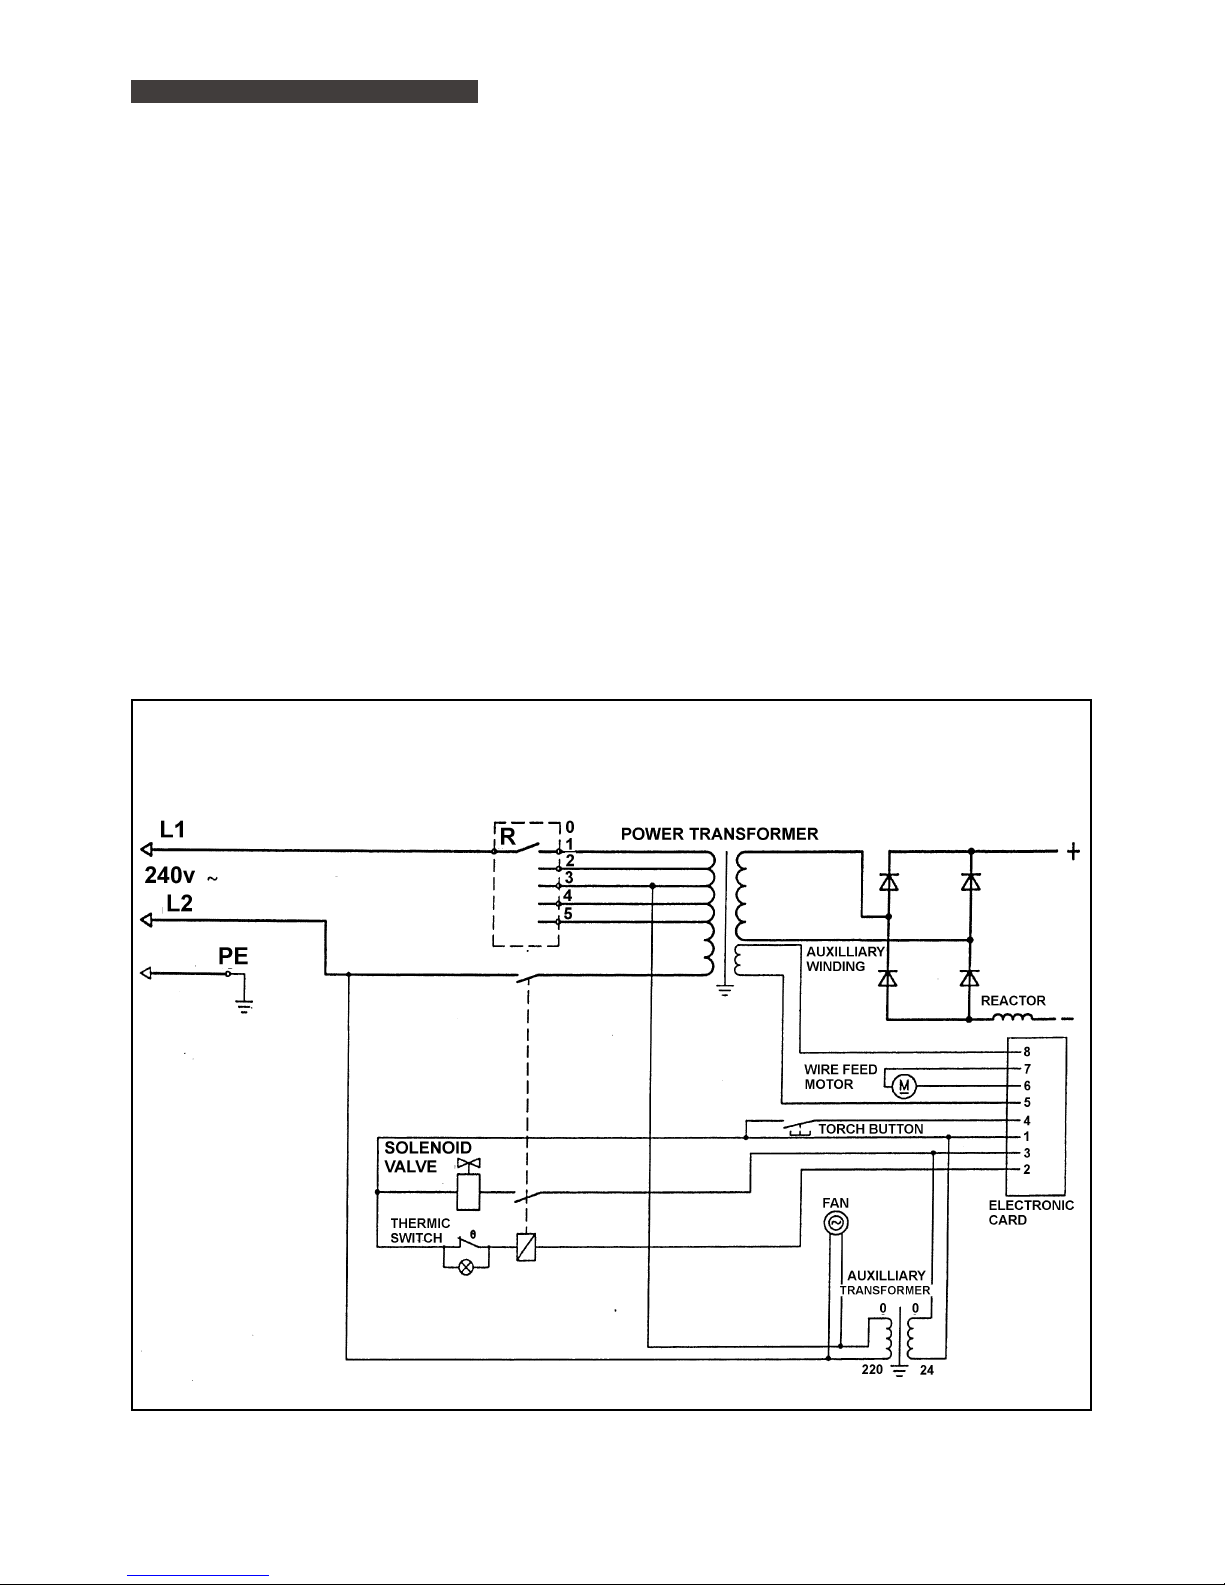
250/10 WIRING DIAGRAM
SUPERMIG 250-Job181-280198
Page 5
Declaration of Conformity
W
e, the sole importer into the UK, declare that the product listed below is in conformity with the following EEC standards and directives.
The construction file for this product is held by the Manufacturer and may be inspected on
request by contacting Jack Sealey Ltd
Models: SUPERMIG250/10
73.23/EEC
Low Voltage Directive (S.I. 1994/3260)
89/336/EEC
EMC Directive (S.I. 1992/2372 & Amendments).
Date 1st March 1998
Sealey Group,
Bury St. Edmunds,
Suffolk.
01284 757500 01284 703534
E-mail:
SUPERMIG 250-Job181-280198
IMPORTANT: NO RESPONSIBILITY IS ACCEPTED FOR INCORRECT USE OF THIS EQUIPMENT.
WARRANTY: GUARANTEE IS 12 MONTHS FROM PURCHASE DATE. PROOF OF PURCHASE WILL
BE REQUIRED FOR ANY CLAIM.
INFORMATION: PLEASE CALL US FOR A COPY OF OUR LATEST CATALOGUE.
1. Power source stops
2. No weld current, fuse blowing in 13amp plug
3. No weld current
4. Feed motor not working, lamp is on
5. W
ire does not feed, feed roller rotates
6. Wire feeds unevenly.
7. Unstable arc.
8. Porous weld
9. Electrode sticking in nozzle
10. Irregular weld head
11. Weld bead too narrow and raised
12. Weld bead too wide
13. Poor penetration
14. Excessive penetration
15. Fuse blowing
Overheating protection activated due to overload
Rectifier blown
Bad connection between clamp & workpiece
Break in earth lead
Break in torch lead
Fuse blown
Gear damaged or worn
Motor defective
Pressure roller improperly adjusted
Dirt, copper, dust, etc, have collection in torch liner
Gas cup (nozzle) defective also check tip
Deformed wire
Dirt, etc, in liner
Gas cup (nozzle) defective
Gas cup (nozzle) spattered
Feed roller groove clogged
Feed roller groove deformed
Pressure roller tension improper
Incorrect settings
Impurities in weld area
Worn or defective gas cup (nozzle)
No gas
Gas cup (nozzle) clogged
Draft blowing away shielding gas
Rusty or dirty joints
Torch too far from or at wrong angle to work
Gas leak
Worn or defective gas cup (nozzle)
Electrode deformed
Wire speed too slow
Torch incorrectly held
Wire weaving in weld pool
Weld current too high
Weld speed too low
Weld current too high
Weld speed too low
Arc too long
Weld current too high
Arc too long
Weld current too high
weld speed too slow
incorrect distance of torch to workpiece
Tension too great
Gas cup contact tip clogged
DEFECT POSSIBLE CAUSE REMEDY (Numbers refer to chapter and item heading)
7. TROUBLESHOOTING
Protection automatically resets when transformer has cooled
(about 15 min).
Replace rectifier.
Clean or grind contact surface and weld area. (4.1),
Repair or replace earth lead.
Repair or replace torch.
Replace fuse 1.5 amp. (6.6).
Replace gears. (6.7).
Replace motor (Contact service agent).
Adjust tension.(3.4).
Clean the liner from the machine forward. Use compressed air.
If too much dirt, replace the liner. (see 6.6).
Replace gas cup (nozzle) and check tip. (6.3 & 6.4).
Check pressure roller tension and adjust it if necessary (3.4).
Clean the liner from the machine forward. Use compressed air.
Replace gas cup (nozzle) and check tip. (6.3 & 6.4).
Clean or replace gas cup (nozzle). and check tip. (6.3 & 6.4).
Clean feed roller. (6.7).
Replace feed roller. (6.7).
Adjust tension. (3.4).
Use recommended settings. (4.1.2).
Clean or grind weld area.
Replace gas cup (nozzle). (6.4).
Open gas cylinder, regulate gas flow.
Clean or replace gas cup (nozzle) and check tip. (6.3 & 6.4).
Screen off welding site or increase gas flow.
Clean or grind workpiece. (4.1).
The distance from gas cup to workpiece should be 8-10mm
and torch angle 60
0
.
Check hoses, connections and torch assembly. (see 6.2.).
Press the gas cup in correction position.
Replace gas cup (nozzle). (6.4).
Check pressure roller tension. (3.4).
See recommendations for wire speed. (see 4.2).
Use torch angle 60
0
. (Chapter 5).
Check pressure roller tension and adjust as needed. (3.4).
Increase voltage and wire speed. (4.2).
Move torch slower and weave a little more.
Decrease voltage and wire speed. (4.2).
Move torch faster and weave less.
Bring torch closer to workpiece.
Increase voltage and wire speed. (see 4.2.).
Bring torch closer to workpiece.
Decrease voltage and wire speed. (see 4.2.).
Move torch faster.
Torch distance should be 8-10mm.
Release tension. (3.4).
Clean gas cup and contact tip. (6.3 & 6.4).
J. Sealey.
Jack Sealey Ltd.
Sealey Power Welders.
 Loading...