

Page 1
OPERATION/MAINTENANCE
MANUAL
Page 2
Page 3
PRO WELD
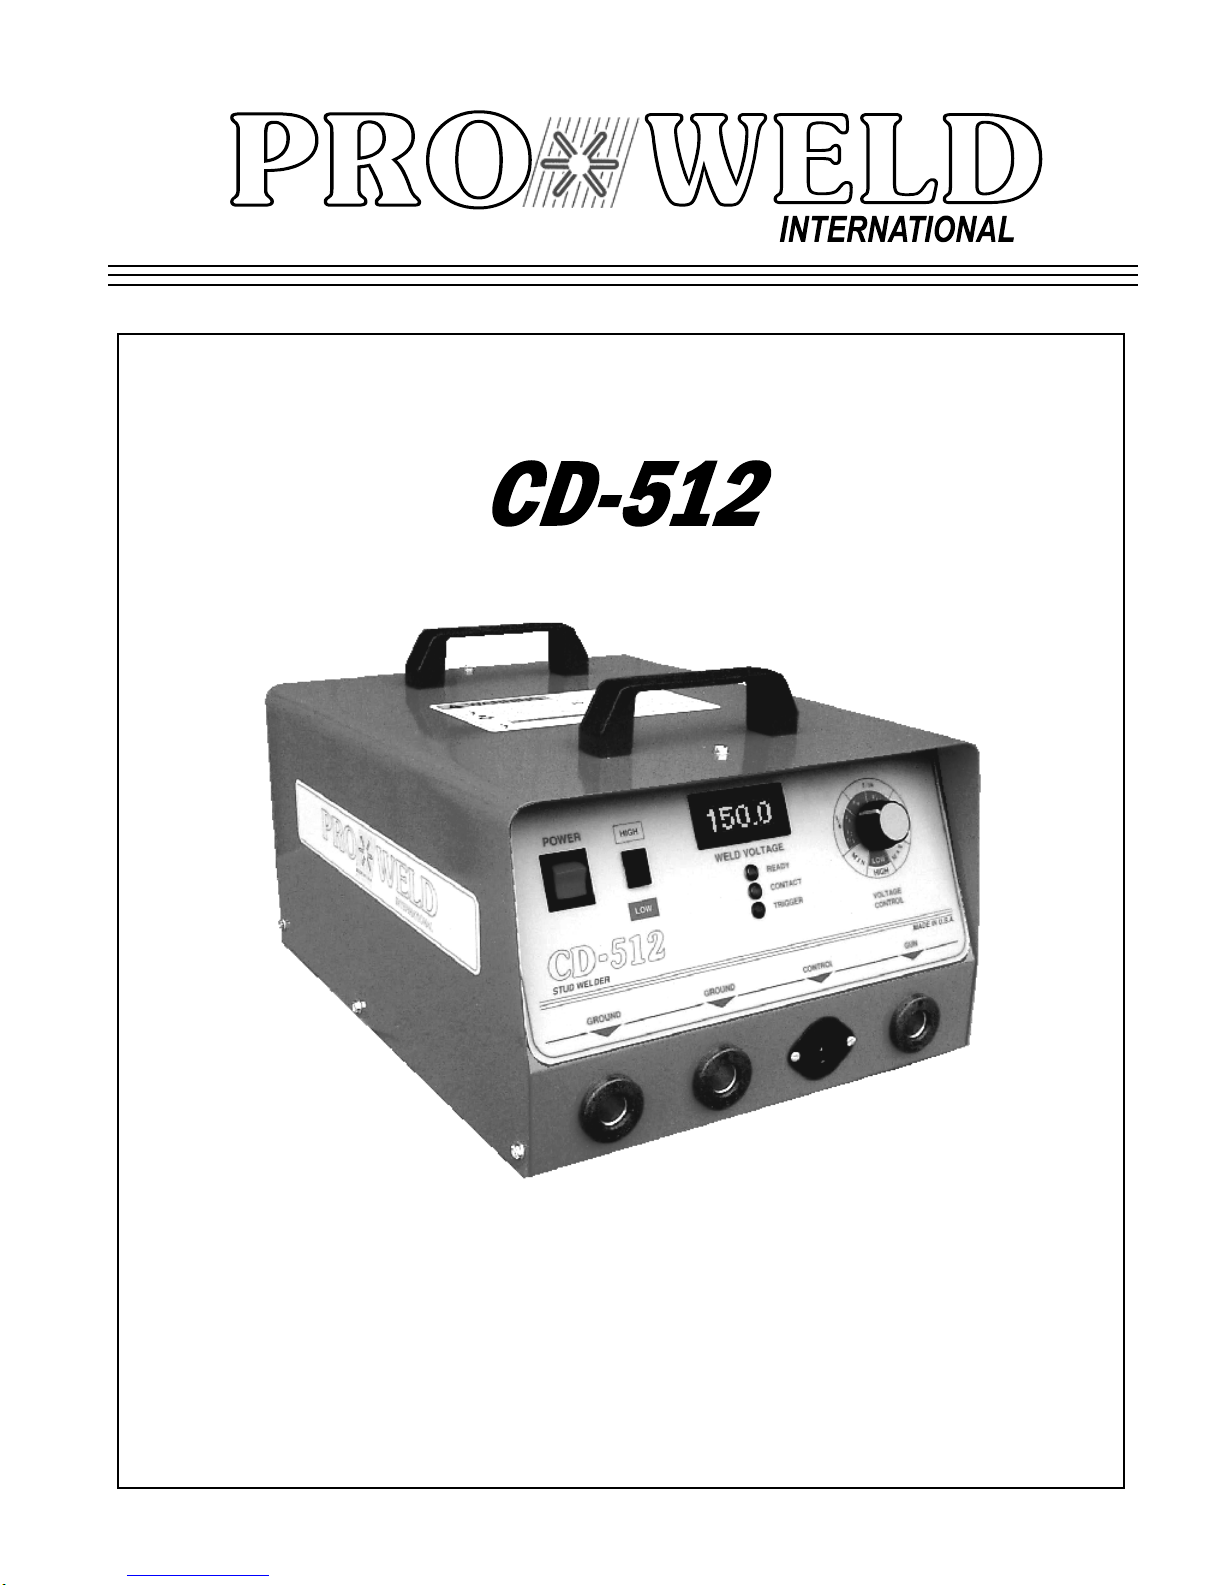
CD-512
1.0
2.0
3.0
4.0
5.0
6.0
7.0
8.0
9.0
10.0
TABLE OF CONTENTS
INTRODUCTION
WARRANTY 1
UNPACKING YOUR UNIT
SUGGESTED SAFETY PRECAUTIONS
GENERA
THE CD WELDING PROCESS
POWER REQUIREMENTS
SYSTEM SPECIFICATIONS
WELDING SYSTEM HOOK-UP
9.1
9.2
SYSTEM OPERATION
L DESCRIPTION
Straight Polarity
Reverse Polarity
1
1
1
2
2
3
3
4
4
5
6
11.0
12.0
13.0
14.0
15.0
16.0
17.0
18.0
GUN SET-UP 8
11.1
11.2
11.3
11.4
11.5
11.6
WELDABLE MATERIAL COMBINATIONS 13
CAUSES OF POOR OR ERRATIC WELDS 14
TROUBLE SHOOTING POOR WELDS 14
ROUTINE WELDER MAINTENANCE 15
ASSEMBLY –CD-512 CONTROLLER
16.1 PC Board Assembly Drawing 19
TROUBLE SHOOTING – ELECTRICAL 20
CHECK LIST CD-512 SYSTEM P.N. 100-0110 22
Standard
Installin
For Weld Pins with Collet Protector
Template Adapter
Collet Protector w
Parts List HD CD Handgun 12
g or Changing Collets or Chucks
ith Blunt Leg 10
10
8
9
9
16,17,18
19.0
CHECK LI
ST CD-512 SYSTEM P.N. 100-0111 22
Page 4

PRO WELD
CD-512
LIST OF FIGURES
1
2 STRAIGHT POLARITY HOOK-UP 4
3
5
6 STANDARD GUN SETUP 8
7
8 TEMPLATE ADAPTER GUN SETUP 10
9
10
11
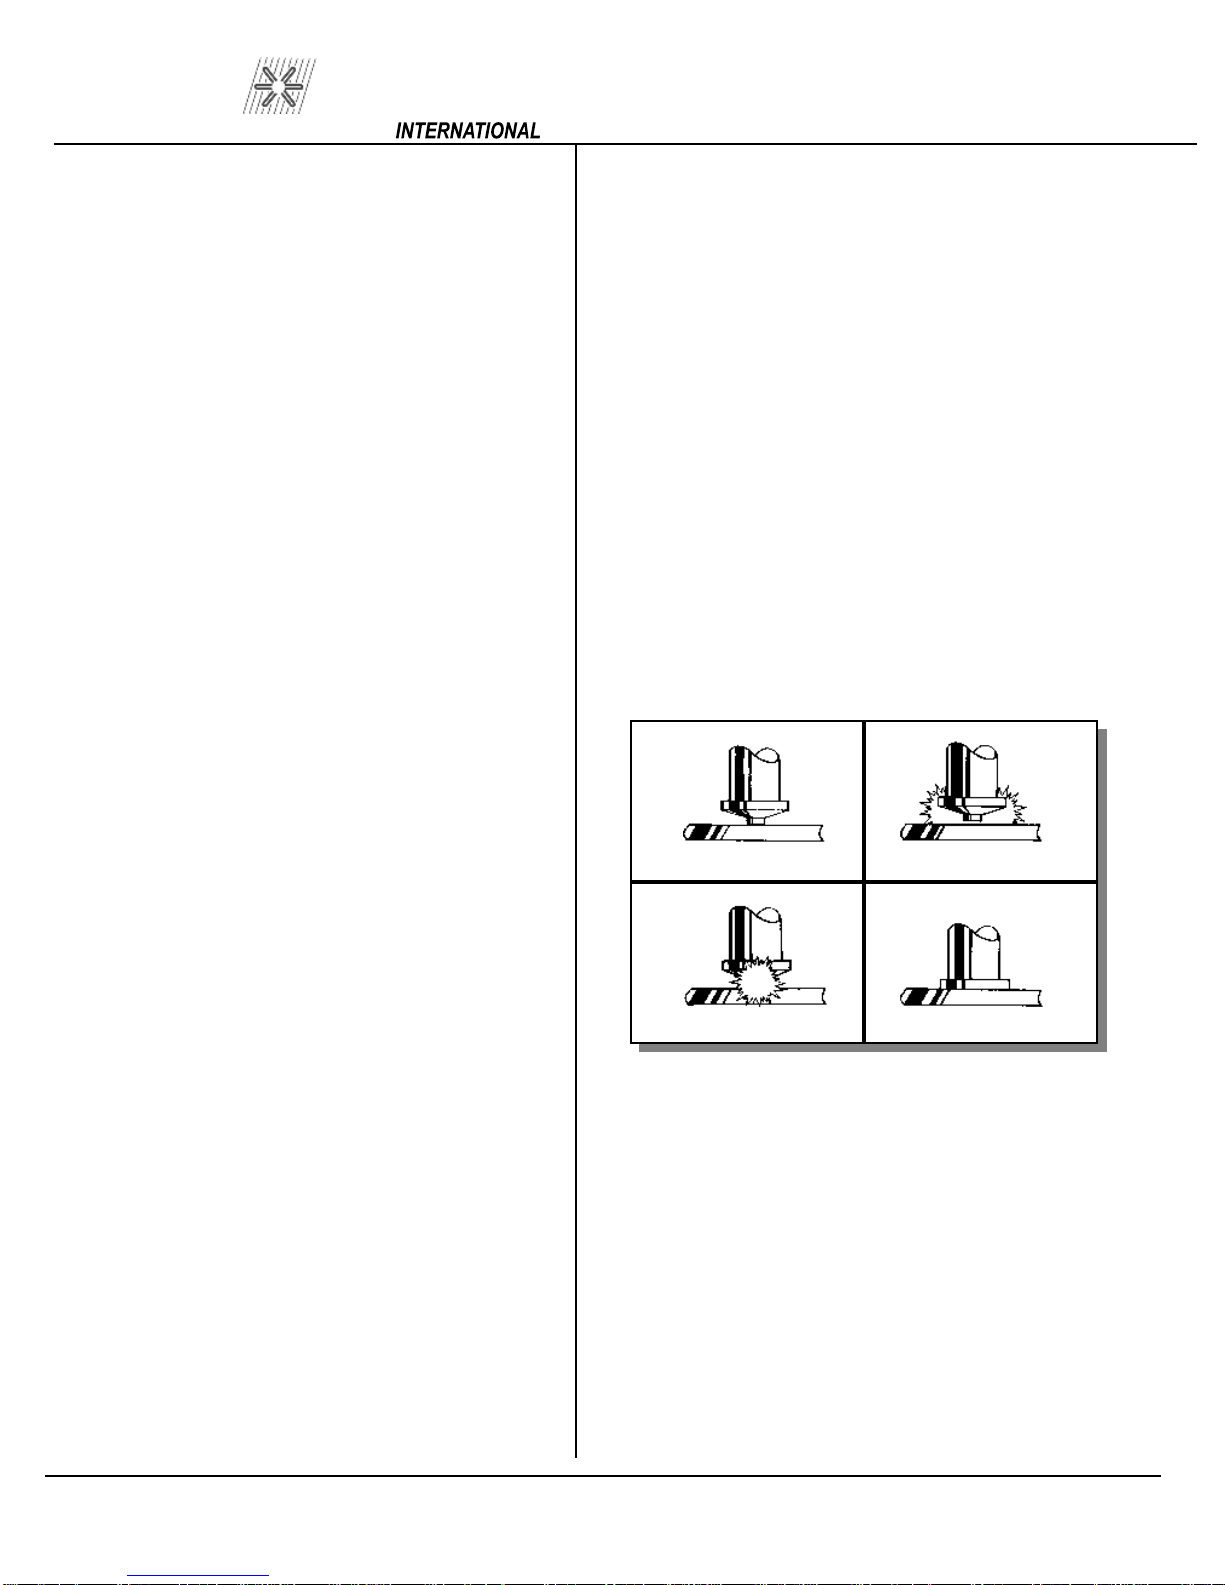
CD CONTACT PROCESS
REVERSE POLARITY HOOK-UP
FRONT PANEL LAYOUT
COLLET PROTECTOR SETUP
COLLET PROTECTOR/BLUNT LEG SETUP
HEA
VY DUTY CD GUN
HOT WELD
14
2
5
6
9
11
10
12
13
14
15
16
17
18
19
COLD WELD
ARC BLOW
WELD WITHOUT FOOTPIECE
GOOD WELD
PARTS LIST
PARTS LIST
PARTS LIST
PC BOARD
14
15
15
16
(continued)
(continued)
19
17
18
15
Page 5

PRO WELD
CD-512
Page 6
PRO WELD
CD-512
Page 7
PRO WELD
CD-512
Page 8
PRO WELD
CD-512
Page 9
PRO WELD
1
.0 INTRODUCTION
Your new stud welding equipment is carefully
constructed of the finest components and materials
available. Used
you years of profitable, efficient service.
The system incorporates the latest in enginee
ing advances, for completely reliable end welding of
mild steel, stainless steel, aluminum and lead free
copper and brass fasten
A careful study of this manual will enable you
to understand how the welder operates to insure
proper performance under al
properly, this equipment will give
2.0 WARRANTY
The electrical and mechanical components of
the stud welder are thoroughly performance i
spected prior to assembly in the welder. The asse
bled welder is completely performance checked. The
welder is delivered to you in functional electro
mechanical condition.
All p
arts used in the assembly of the welder
and its accessories are fully warranted for a period of
1 YEAR from the date of delivery
welding capacitors are warranted for a period of 1
YEAR from the date of delivery. The printed circuit
boards
for a period of 3 years.
the right to repair or replace, at their option, defe
tive parts which fail during the guarantee period.
No
ment must be furnished to the manufacturer by the
purchaser within ten (10) days after the defect is first
discovered. The manufacturer does not assume any
liability for paying shipping cost or any labor or m
terials furnished where such cost are not expressly
authorized in writing.
acces
abuse, improper installation, maladjustment, or use
not in accordance with the operating instructions fu
nished by the manufacturer. The warranty is valid
only when studs are purchased from sources a
proved by the manufacturer or are of identical spec
fi
used in all proweld equipment are warranted
Under the warranty, the manufacturer reserves
tice of any claim for warranty repair or replac
The manufacturer does not warrant any parts or
sories against failures resulting from misuse,
cations to the manufacturer’s
ers.
l operating conditions.
. In addition, the
n-
m-
-
c-
e-
a-
p-
CD-512
3
.0 UNPACKING YOUR UNIT
possible to the point of installation before unpacking
it. Do not operate the unit from an extension power
r-
cord if possible. Once the unit is unpacked it is reco
mended that you inspect it for any physical damage.
inspected at the factory. Upon
hooked up to the recommended incoming power b
fore welding. We recommend that you check that you
have received all the items listed on the shipping
check list. (see SECTION 1
adequate ventilation. Do not restrict the air flow
through the side l
the control housing.
Upon receipt of your unit, place it as close as
Your unit has been completely assembled and
receipt, the unit must be
8 or 19)
Place the unit in a large enough area to provide
ouvers. Do not allow water to enter
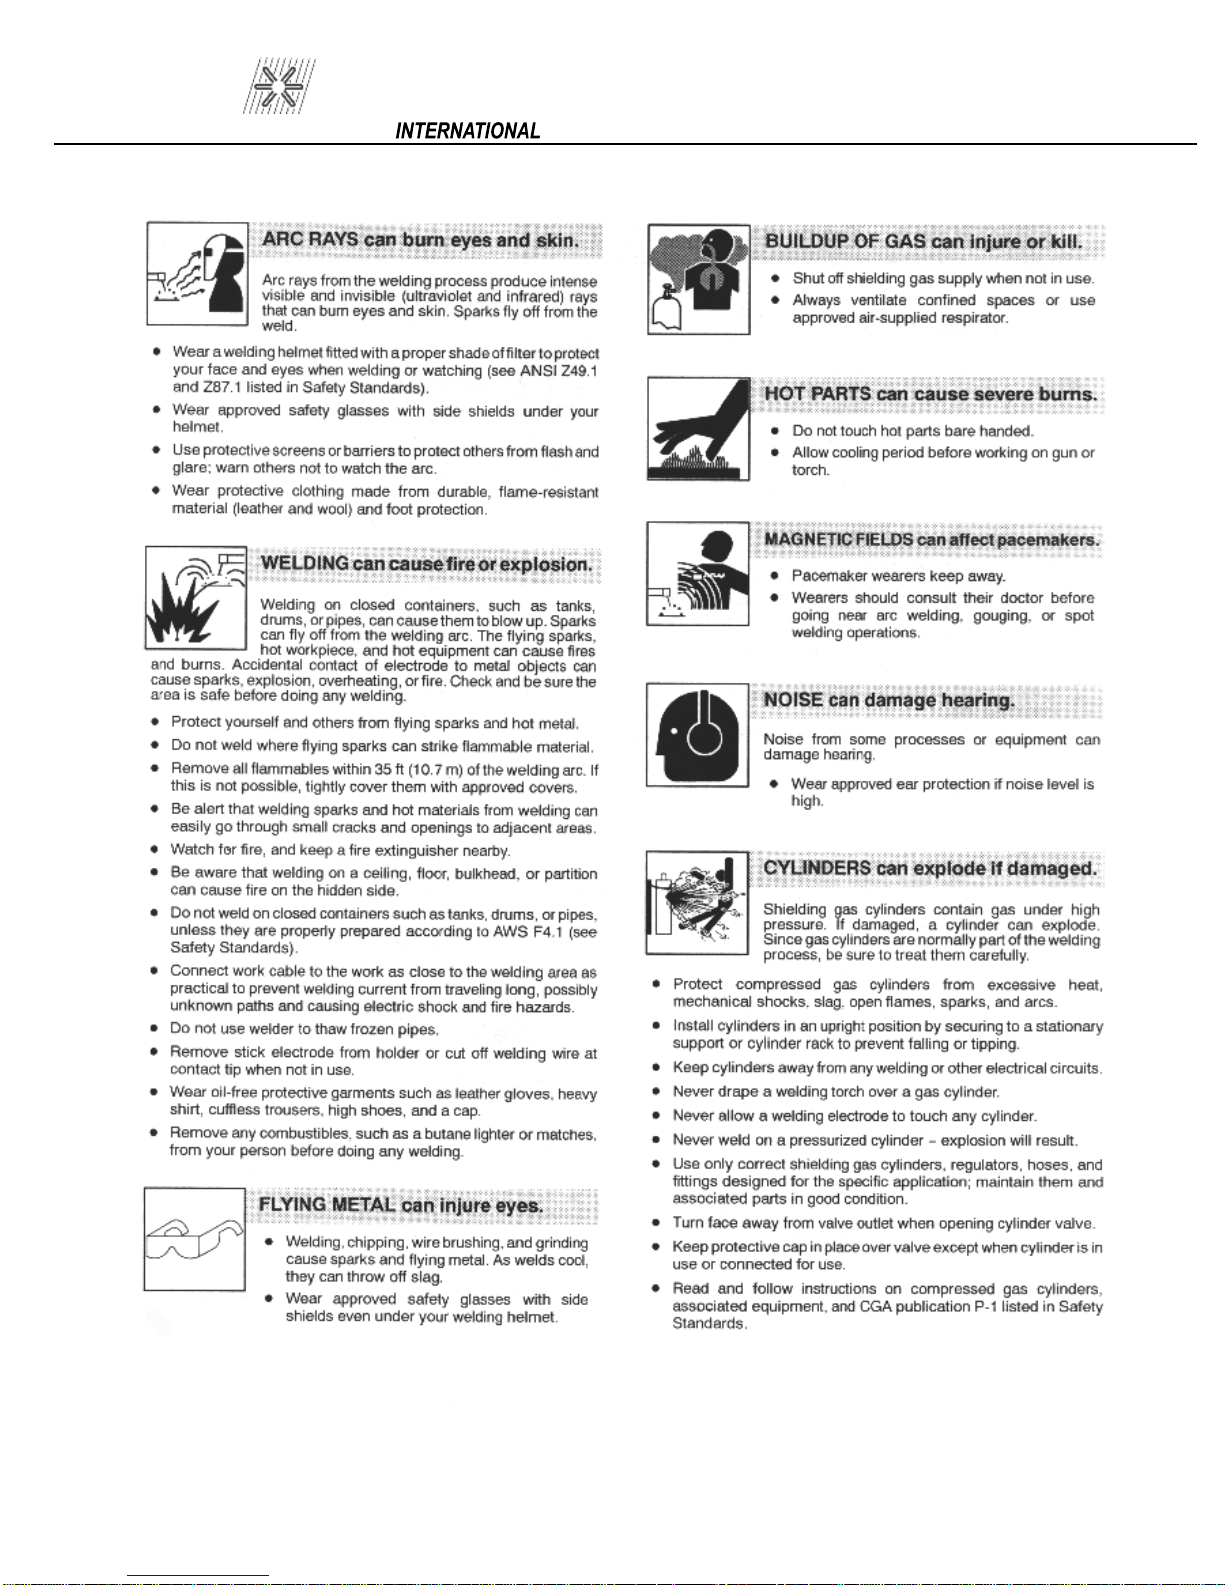
4.0 SUGGESTED SAFETY PRECA
TIONS
ity of the welder to observe certain safety rules to i
sure his personal safety and to protect those working
near him.
Reference is directed, without endorsement or
recommendation, t
and Cutting, and to AWG Publication A6,1-66, Re
om
ing.
r-
i-
while welding or weld in the rain. Avoid wear-
In any welding operation, it is the responsibi
o ANSI Z49.1, Safety in Welding
mended Safety Practices for Gas-Shield Arc Wel
1. Always treat electricity with respect. Under
open circuit conditions, the welding machine
output voltage may be dang
2. Don’t work on live circuits or conductors.
Disconnect the main power line before check
ing the machine or perform
nance operations.
3. Be sure the welding machine cabinet is
properly grounded to a good electrical ground.
4. Don’t stand in water or on a damp floor
ing wet sweaty cloths when welding.
U-
erous.
ing any mainte
m-
e-
l-
n-
c-
d-
-
-
PAGE 1
Page 10
PRO WELD
5. Don’t operate with worn or poorly con
nected cables. Don’t operate weld gun with
loose cable connections. Inspect all cable
quently for insulation failures, exposed wires,
loose connections, and repair as needed.
6. Don’t overload welding cab
to operate with hot cables.
7. Don’t weld near flammable materials or liq
uids, in or near atmospheres, or o
ing explosive gases.
8. Don’t weld on containers which have held
combustible or flammable materials, or on ma
terials which give off flammable or toxic va
pors when heated, without proper cleaning,
purging, or inerting.
les or continue
n ducts carry
-
s fre
CD-512
1
10 volt AC line voltage. The system comes complete
with power cord, weld cables and gun. Just add the
-
-
-
-
-
accessories required for t
This manual should provide all the information r
quired for you to be able to set up, weld, and maintain
the CD-512 welding system.
6.0 THE CD WELDING PROCESS
common method of CD stud welding. Practically
foolproof, it produces no reverse side marking in
most cases and is suitable for most commercial and
industrial applications.
accessories for the length and diameter stud you are
going to weld. Refer to the CD Acc
and CD Stud Welding Gun Section for information
on accessories and gun set
Contact welding
First
, the gun must be set
he stud size to be welded.
e-
is the simplest and most
-up with the proper
essories Guide
-up.
9. Be sure t
when welding in confined spaces.
10. Never look at the electric arc without wear
ing protec
11. Always use the proper protective clothing,
gloves, ect.
12. Never strike an arc when near a bystander
who is unaware of the dangers of ultraviolet
light on their eyes.
5.0 GENERAL DESCRIPTION
CD-
tained heavy duty capacitor discharge power supply
capable of welding up to 5/16” flanged studs in mild
steel or stainless steel
It can weld up to 1/4 flanged studs (5/16” weld base
diameter) in aluminum or brass.
for longer life and has been designed for easy mai
te
nance and field service. This welder uses standard
512 HEAVY DUTY PORTABLE
CD ST
The CD-512 portable CD welder is a self co
The CD
o provide for proper ventilation
tive eye shields.
UD/PIN WELDER
(3/8” in weld base diameter).
-512
utilizes a solid state control board
n-
n-
1 2
-
Initial Contact
3 4
Forced Into Molten Pool
(FIGURE 1 CONTACT CD WELD)
base material (SEE FIGURE 1). Verify that the gun is
held perpendicular to the work
di
porizes the tip. The proper tip design is critical. This
is what determines the length of time of the weld. An
arc is briefly sustained which melts the stud base su
face and the work surface directly underneath the
stud. The spring pressure in the gun then forces the
stud into the molten pool, completing the weld in a
proximately six milliseconds.
The stud is first placed in contact with the
scharges the capacitors through the stud which v
During Weld
After Weld
. Pulling the trigger
a-
r-
p-
PAGE 2
Page 11
PRO WELD
T
his technique, when equipment is set up properly,
is simple and easily mastered. The same power su
ply is capable of welding many different sizes and
materials of fasteners. If you require assistance in
selecting the proper accessories, contact our cu
tomer service department or your field represent
tive.
7.0 POWER REQUIREMENTS
110 VOLT OPERATION
110 volt AC 60 H:
Internal Fusing
Integral 9 foot power cord
:
25 amp service
BUSS ABC 25 amps;
slo
w blow;
P/N 120
-0025
s-
a-
p-
CD-512
Capacitance:
84,000 uF nominal Low Range
168,000 uF nominal High Range
Weld Mode:
Polarity:
Powe
Internal Fusing:
STAN
Contact
Straight or Reverse
r Required:
110 Volt AC 60 Hz 25 Amp
BUSS ABC 25 Amp Slo-Blow(110V)
3AG 1 Amp 250 volt (2 on PC board)
DARD GUN & CABLE SPECIFICATIONS
IF EXTENSION REQUIRED
Cable Length
50
12’
25’
30’
110 Volt
#16/3
#16/3
#14/3
#12/3
8.0 SYSTEM SPECIFICATIONS
Weight:
64 Lbs.
Size:
Chassis:
Panel Controls:
Weldable Materials:
Brass, Zinc coated, Galvanized
Weldable Stud Diameter:
Weld Rate:
Weld Voltage:
45-
8 1/2” H x 13 1/4” W x 20” D
21.6 cm H x 33.7 cm
16 Ga. Steel (Painted International Orange)
Power
Voltage Control
Steel, Stainless steel, Aluminum, Copper,
12 Ga. Through 7/16” Weld Base
(Max W.B. Dia. For AL=5/16” {1/4” thread})
24 per minute 5/16”
185 VDC
W x 50.8 cm D
WELD GUN-LIGHT DUTY PRECISION
CD CONTACT
Part Number:
300 300-
Weight:
2 lbs. (not including cable)
Size:
6
Weldable Stud Diameter:
Material:
Integral Gun Cable Length:
Connectors:
Cable
Ground Cable:
( lbs. (including 25 ft. #4 weld cable & 16
SOW control cable)
1/2” x 5 3/4” x 2”
12 Ga. Through 7/16” W.B. Dia.
High strength, impact resistant, glass fi
inforced polycarbonate
25 feet – #1 AWG
Male Camlok / 2 Pin Hubbell Male
s
(2) #1 x 15’
0200 HD B Collet Gun
0201 HD
Taper Tip Gun
(P/N: 125-0101)
ber re
-4
-
PAGE 3
Page 12
PRO WELD
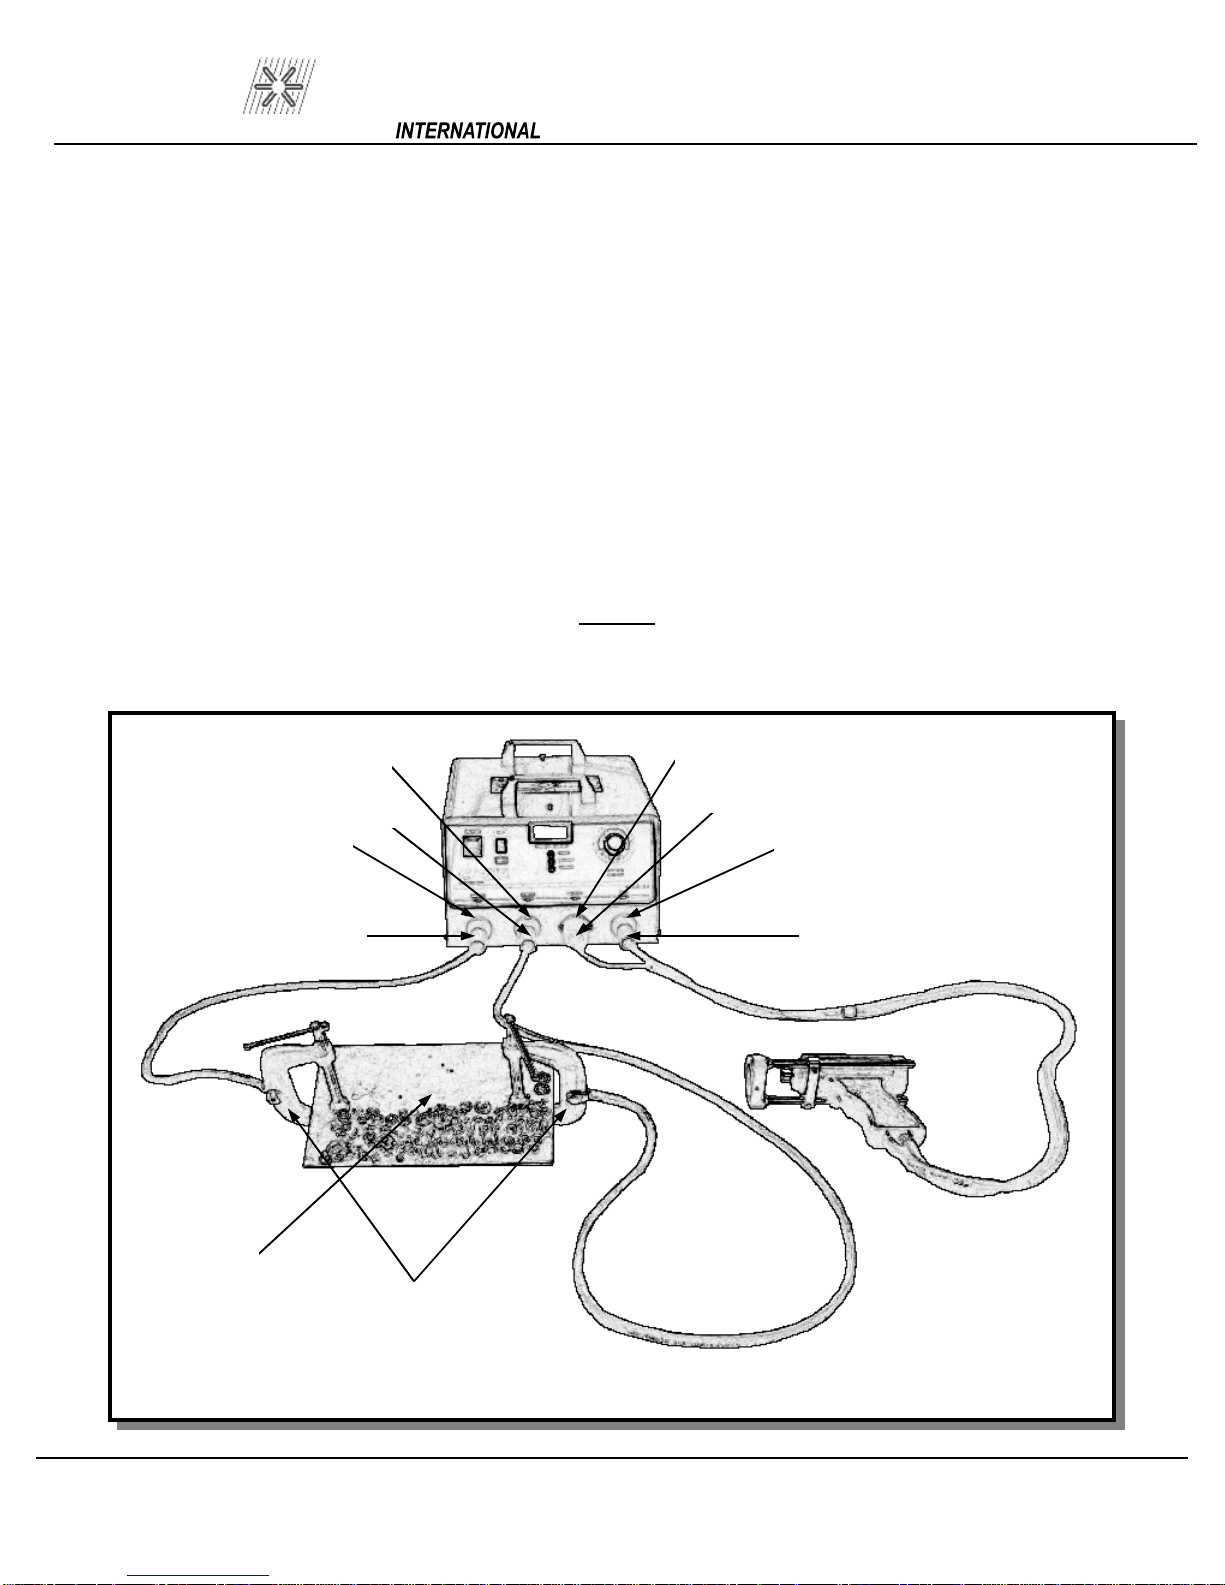
9.0 WELDING SYSTEM HOOK-UP
9.1
A. Connect ground ca
receptacle marked GROUND. Twist until it locks. Atta
(CLEANED AREA).
B. Connect the gun control cable (3A) into the female receptacle (3).
C.
locks.
D. Connect AC power cable to AC outlet.
The gun welding and control cables must be laid out in a straight line. Poor weld quality may
result if wel
Straight Polarity (Standard Set-Up) (see Figure 2(shown with dual grounds))
ble connector (1A) into camlok (1). The camlok should be connected into the
Connect the gun weld cable (4A) into the receptacle marked GUN (4). Twist clockwise until it
ding cables are coiled.
ch “C” clamp (2) to the workpiece (5)
NOTE:
CD-512
1
1A
1
1A
5
2
3
3A
4
4A
PAGE 4
Figure 2 Straight Polarity Hook-Up
Page 13
PRO WELD
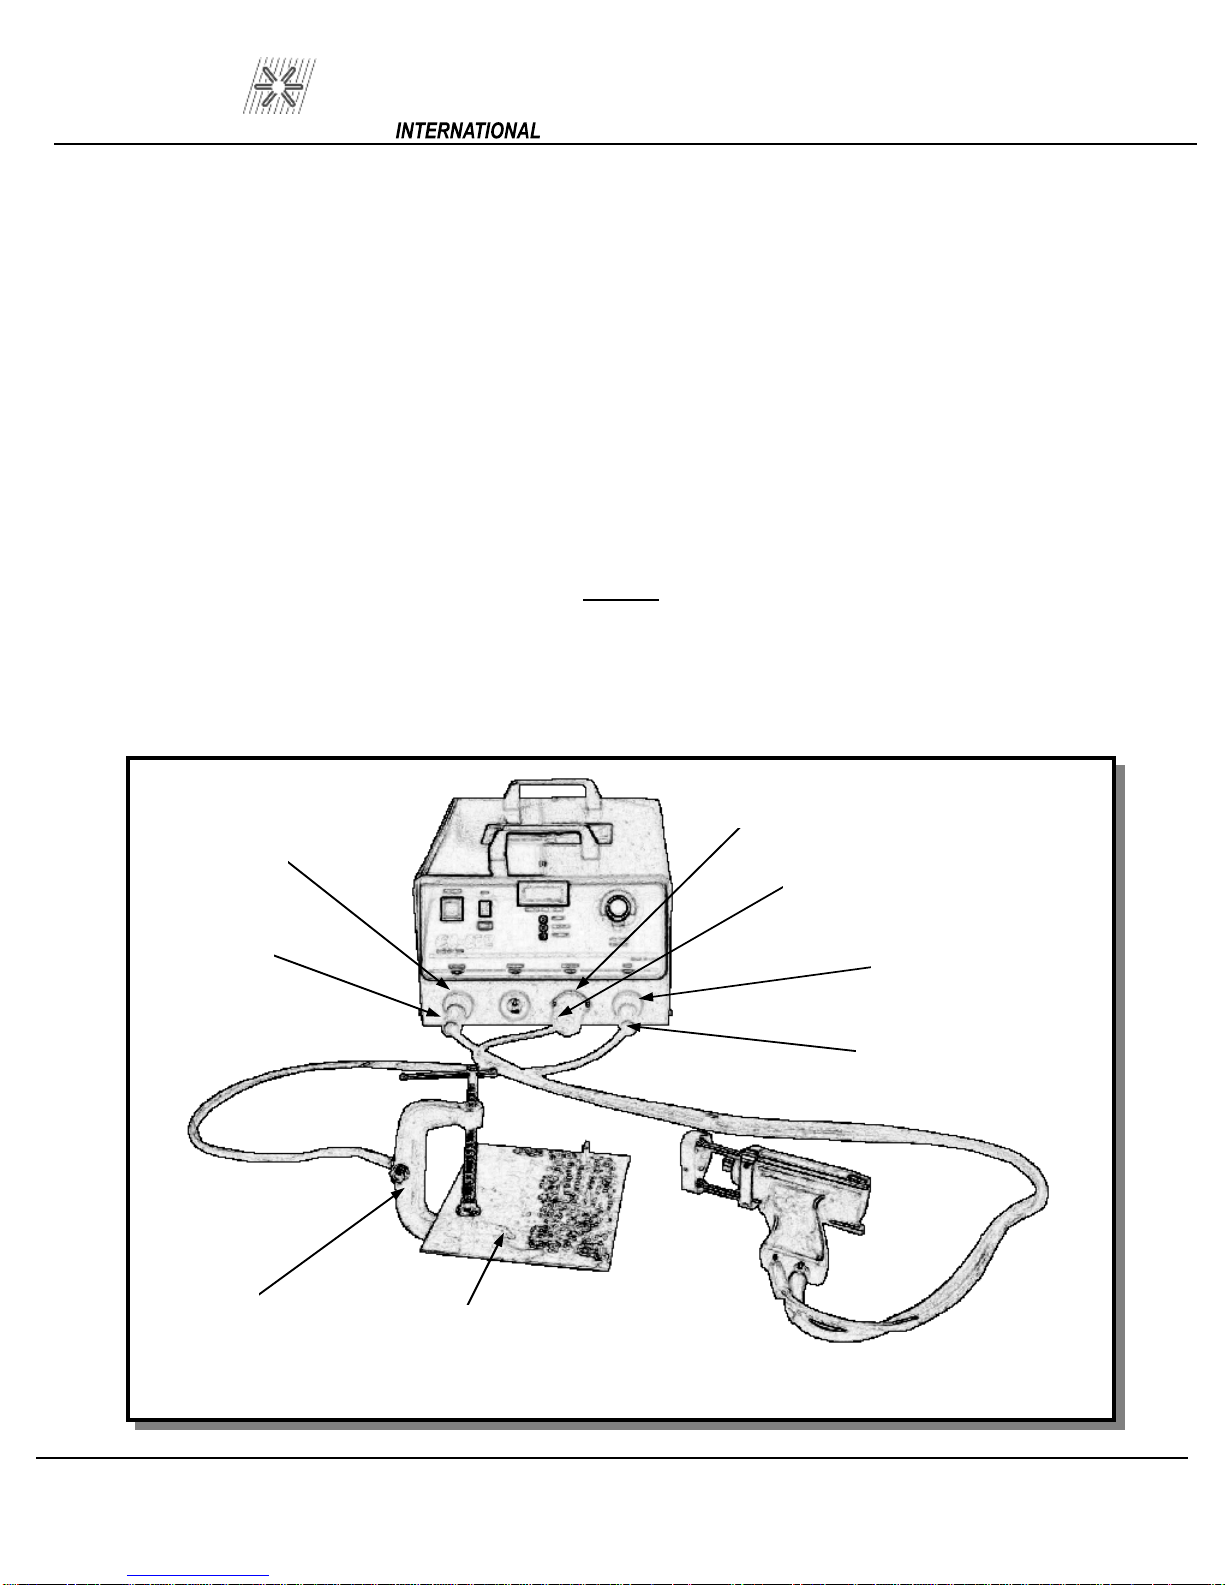
9.2 Reverse Polarity (Recommended for brass or galvanized) (see Figure 3)
A. Connect ground cable connector (1A) into camlok (
receptacle marked GUN. Twist until it locks. Attach “C” clamp (2) to the workpiece (
AREA).
B. Connect the gun control cable (3A) into the female receptacle (3).
C. Connect the gun weld cable (4A) in
it locks.
D. Connect AC power cable to AC outlet.
The gun wel
result if welding cables are coiled.
ding and control cables must be laid out in a straight line. Poor weld quality may
to the receptacle marked GROUND (1). Twist clockwise until
CD-512
4). The camlok should be connected into the
5) (CLEANED
NOTE:
4A
2
3
1
5
Figure 3 Reverse Polarity Hook-Up
3A
4
1A
PAGE 5
Page 14
PRO WELD
1
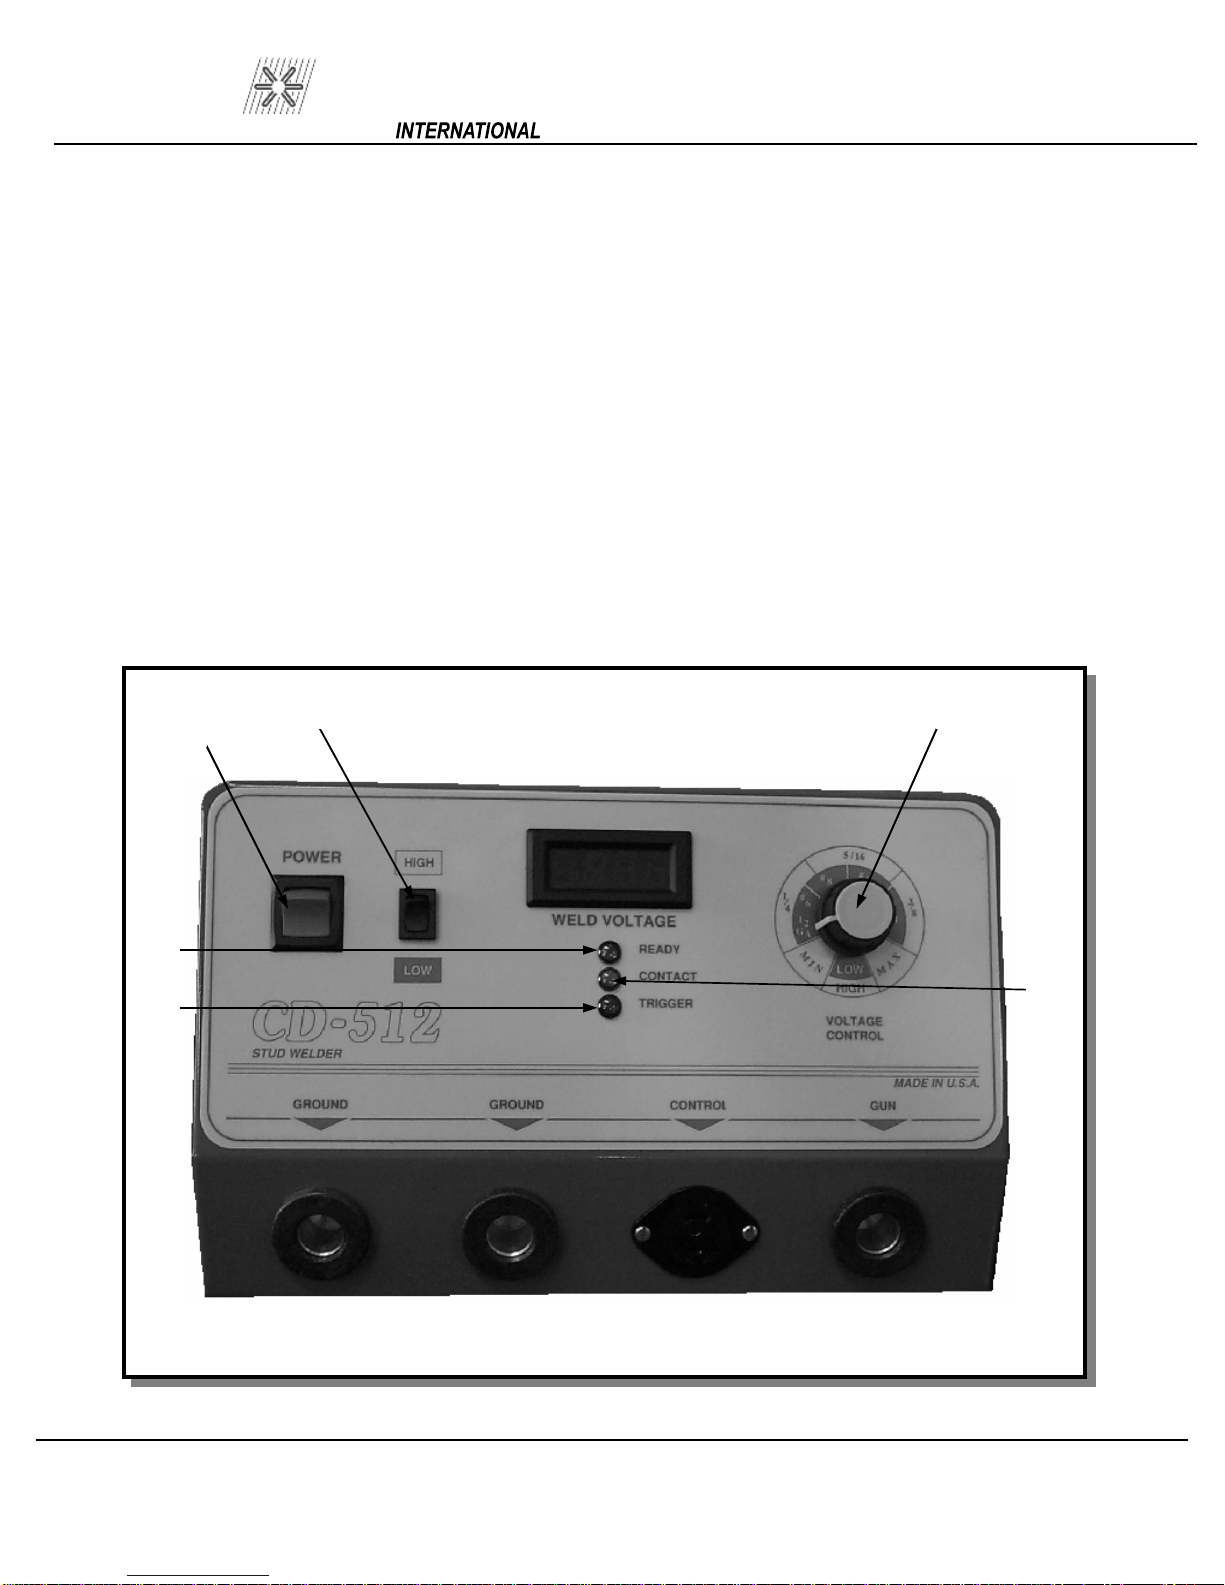
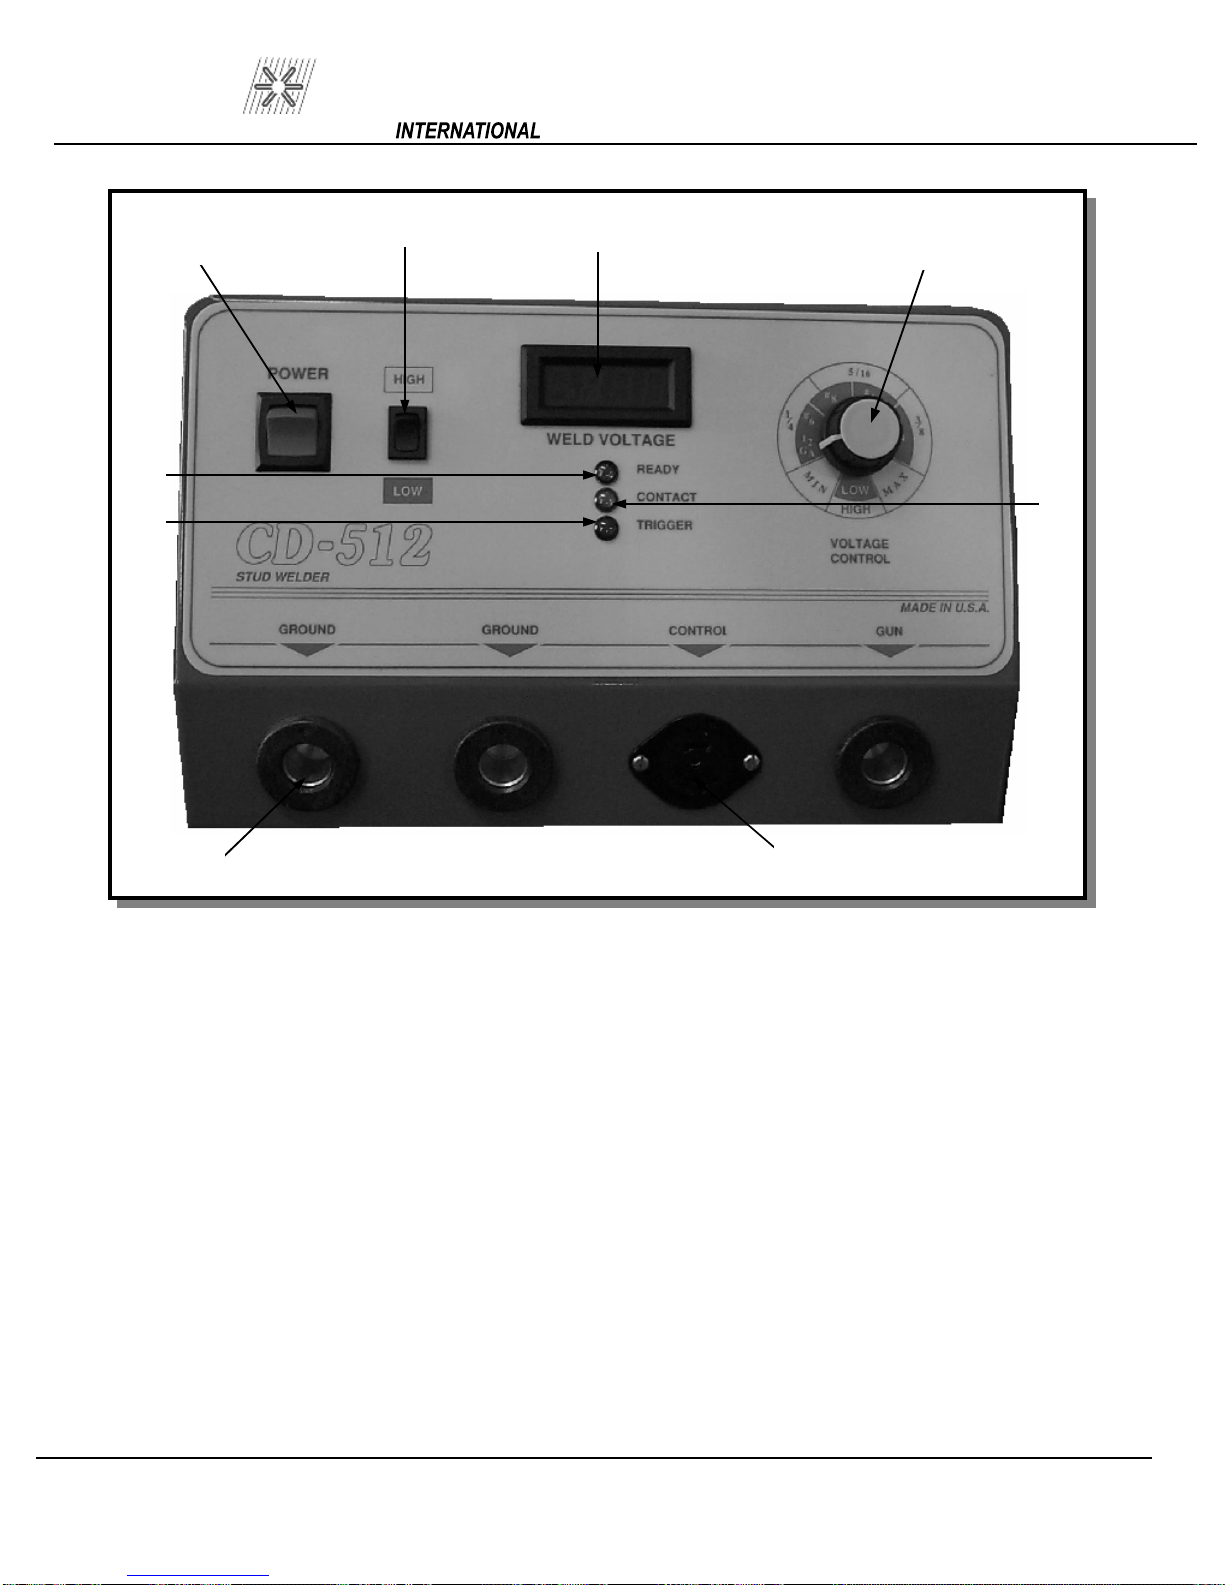
0.0 SYSTEM OPERATION
(see Figure 4)
CD-512
1.
2.
variable voltage control dial (3) a ready indicator light (4
the front panel.
3.
to the lowest setting.
4.
tion. The integral indicator light (1) will turn on.
5.
The CD-512 is designed for simple, yet precise operation.
It has an “ON-OFF” toggle
Before turning the unit “ON”, the voltage control knob (3
With all cables connected, turn the unit on by putting the rocker switch (1) in the “ON” pos
When the capacitors reach the charge voltage setting, the ready light (
2 3
1
switch/indicator light (1) a High/Low range selection switch (2),a
), a contact light (5) and a trigger light (6) on
) should be turned counter-clockwise
i-
4) will turn on.
4
6
PAGE 6
5
Figure 5 Front Panel Layout
Page 15
PRO WELD
S
etting the Weld Voltage/Capacitance
clockwise to increase the weld voltage until the
indi
number for the particular stud size that you are
welding. (See the set up information
Once the voltage control knob is set to
a higher setting, turning it counterwill NOT reduce the volta
bank, until the toggle switch (1) is turned
“OFF” (for approximately 10 seconds).
ages corresponding to various stud sizes. The
approximate voltages for each stud size is as
follows:
45 –
65 –
95 –
120 –
145 –
180 –
Slowly turn the voltage control knob
cator knob is pointing at the appropriate
chart).
NOTE:
clockwise
ge on the capacitor
The settings are marked with the vol
LOW RANGE
60 VDC
95 VDC
120 VDC
145 VDC
180 VDC
185VDC
#8
#10
Min.
12 ga.
1/4”
MAX.
t-
CD-512
60 –
100 –
140 –
The voltage charge on the capacitor bank is read on
the digital panel meter. The ready light indicates
when the capacitors are charged and a stud may be
welded.
Contact Light
ceptable electrical connection between the stud and
ground. This light will turn on when the stud is
placed in contact with the ground.
Trigger Light
The trigger light indicates there is a co
plete circuit to the unit through the gun control c
ble and switch. This light will turn on when the gun
trigger is pressed.
HIGH RANGE
100 VDC
140 VDC
170 VDC
The contact light indicates there is an a
1/4”
5/16”
3/8”
c-
m-
a-
PAGE 7
Page 16
PRO WELD
11.0 GUN SET-UP
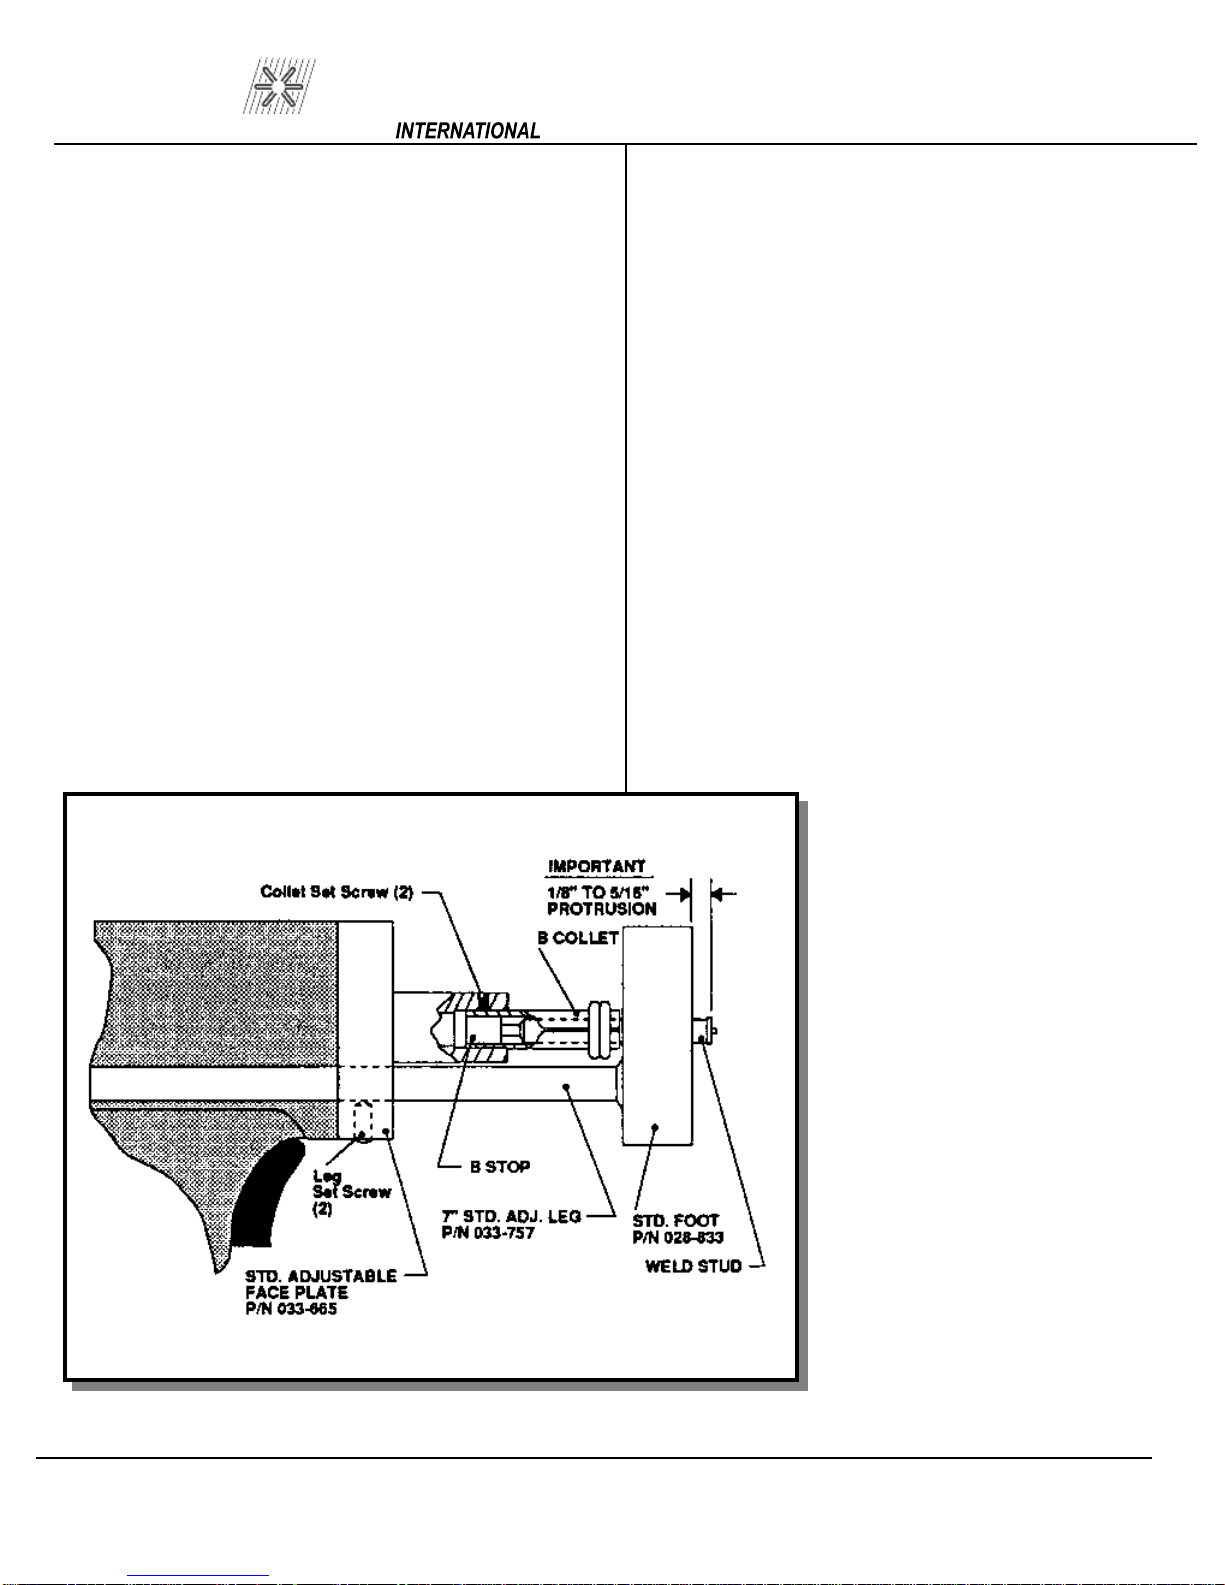
11.1 STANDARD (see Figure 5)
The standard gun set-up is used for welding the
majority of applications. It co
adjustable face plate, two legs, a foot, B-collet, stop,
and spring for your specific stud size.
A step
to set-up and operate the standard CD gun.
To prepare for stud welding, it is necessar
have the proper accessories for the stud to be
welded. Those required are the legs, footpiece,
spring, collet, and appropri
A 3/32” and a 5/32” hex wrench are the only tools
needed for the adjustment of the gun.
-by-
step explanation of the correct way
nsists of the standard
y to
ate screws and washers.
CD-512
For CD welding, the stud normally should be
engaged for all but 1/4” of its length, whenever po
si
ble. Selecting the proper stop will accomplish this
for you. The objective of the collet is to maintain a
firm grip on the faste
and a good electrical connection, yet allow for ease
of loading.
made, assembly may begin. The footpiece is
mounted on the legs using 10-32 x 3/4” socket head
cap screws, inse
the footpiece. These holes are recessed so that the
head of the screws will not protrude.
the collet and stop into the open end of the gun shaft.
Secure the collet in p
shaft. Locate the legs, with footpiece attached, in the
Once the selection of the cor
After assembling the legs and footpiece, insert
ner to assure correct alignment
rect accessory is
rted through the holes at the base of
lace with two set screws on the
s-
Figure 6 Standard Gun Setup
h
oles provided in the gun faceplate. (It
may be necessary to back off the
socket screw in the faceplate to allow
the legs to ente
opening of the footpiece around the
weld end of the fastener. Tighten the
footpiece in position at this time. A
justment for the plunge which is the
distance the stud protrudes beyond the
end of the footpiece can now be made.
This is done b
32 x 1/4” set screws at the bottom of
the faceplate using the 3/32” Allen
wrench. Then sliding the legs f
proper adjustment. Refer to the set
chart for correct plunge distance (from
1/8” to 5/16”).
Correct set-up on all CD
1/8”- 5/16” plunge. This must be a
sured for proper weld results in all
cases.
r the hole). Center the
y loosening the two 10
or
-up
NOTE:
units is
d-
-
s-
PAGE 8
Page 17
PRO WELD
The gun is now ready to weld. Select the
proper setting for the size stud to be welded. Voltage
is determined by the weld base d
your power source is set for the proper polarity:
straight for steel, reverse for galvanized.
11.2 INSTALLING
OR CHUCKS
( The terms collet or chuck are different names for
the same device). The collet holds the pin or
be welded. It is secured to the gun shaft by two set
screws. These screws are loosened to remove or r
place a collet. Tighten these screws snugly to secure
the collet in place.
weldin
collet. If a collet becomes damaged or broken, it
must be replaced. You may also need a stop.
When you change the size of the stud you are
g, you must also change to the appropriate
OR CHANGING COLLETS
iameter. Be sure
stud to
e-
CD-512
therefore, the same setup is applicable
There are two standard sizes
And 10 ga. It is used with the round faceplate and
three blunt legs. The collet protector slides over the
coll
screws. The insert, which takes the place of the I
teral stop, is replaceable.
The stud is pushed into the chuck until the flange bo
toms out on the insert. The collet protector is not
available for studs larger than 10 ga.
1. It does not require a pin stop.
for a range of pin lengths.
2. There is a fixed
adjustments necessary.
3. It provides stability at the weld end
of the pin.
et and fastens to the chuck with three allen set
plunge, no gun
available: 12 ga.
n-
t-
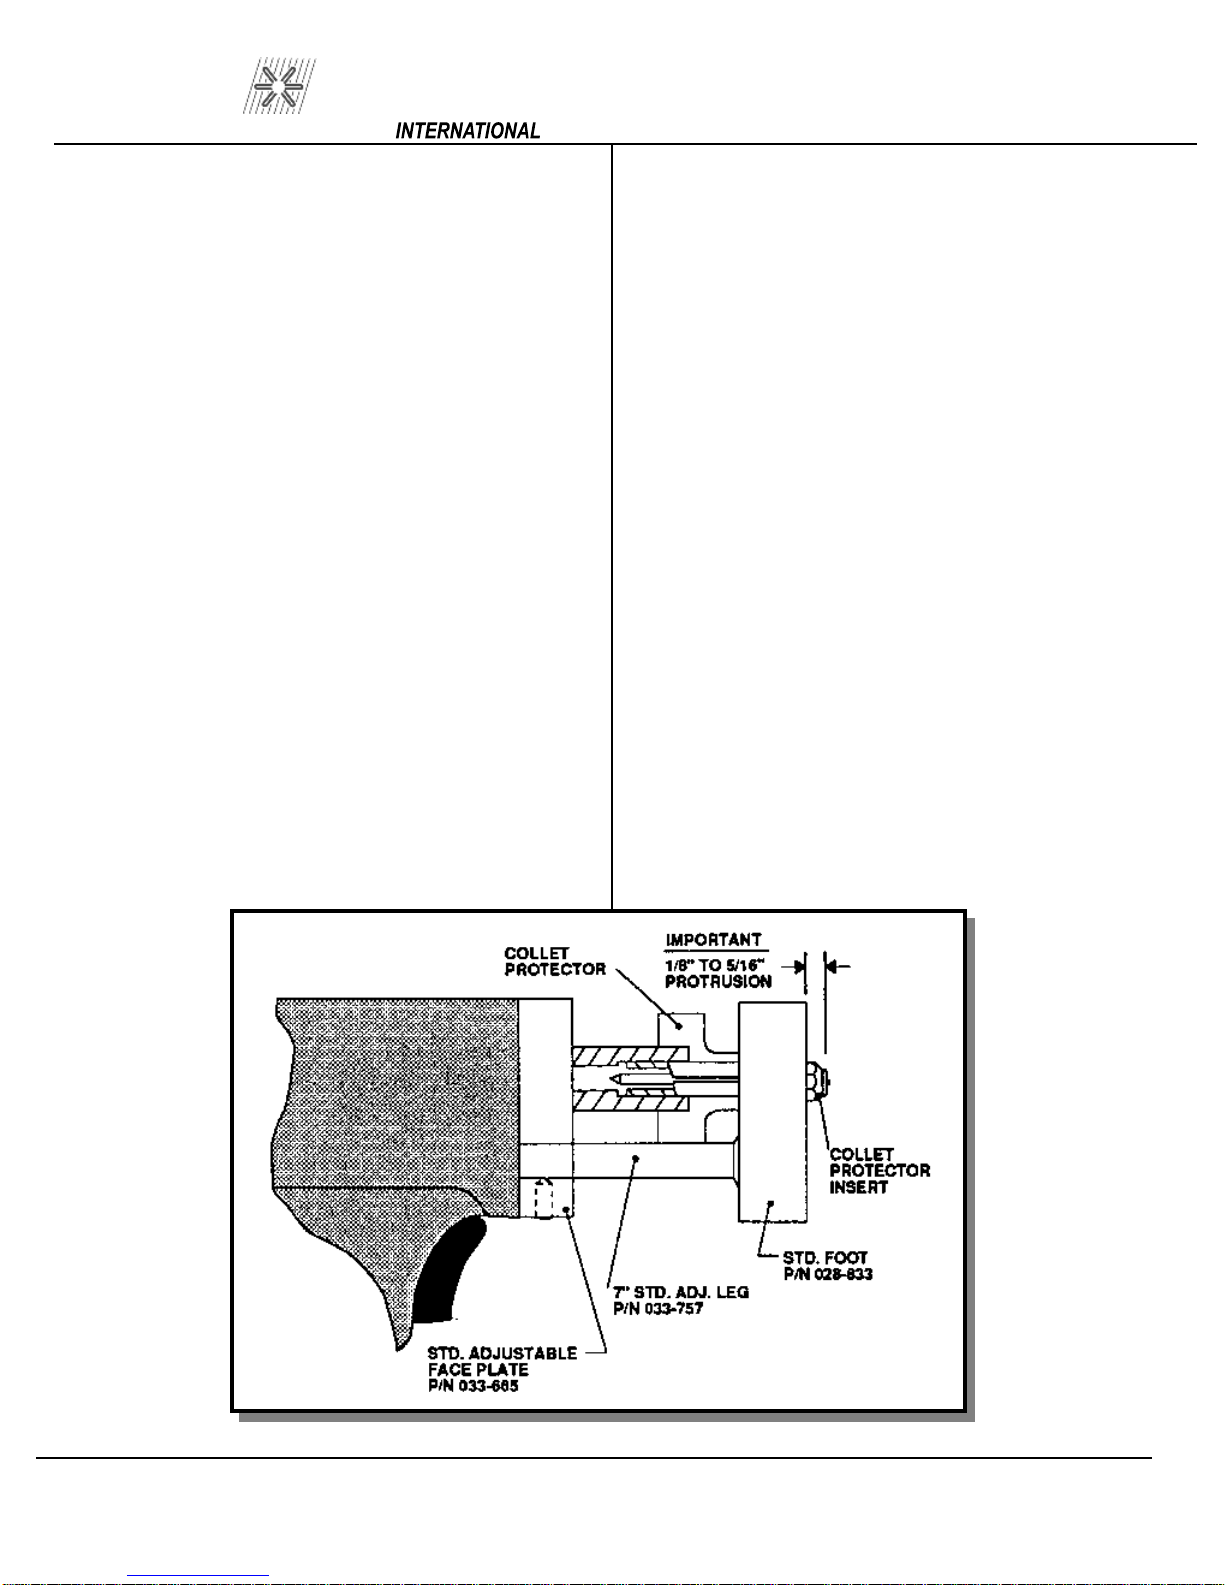
11.3 GUN SET-UP FOR WELD PINS WITH
COLLET PROTECTOR (see Figure 6)
The collet protector has several advantages
over the standard set
-up.
combination can alternately be used with the collet
protector as shown in Figure 7.
The standard adjustable legs and footpiece
Figure 7 Collet Protector Gun Setup
PAGE 9
Page 18
PRO WELD
1
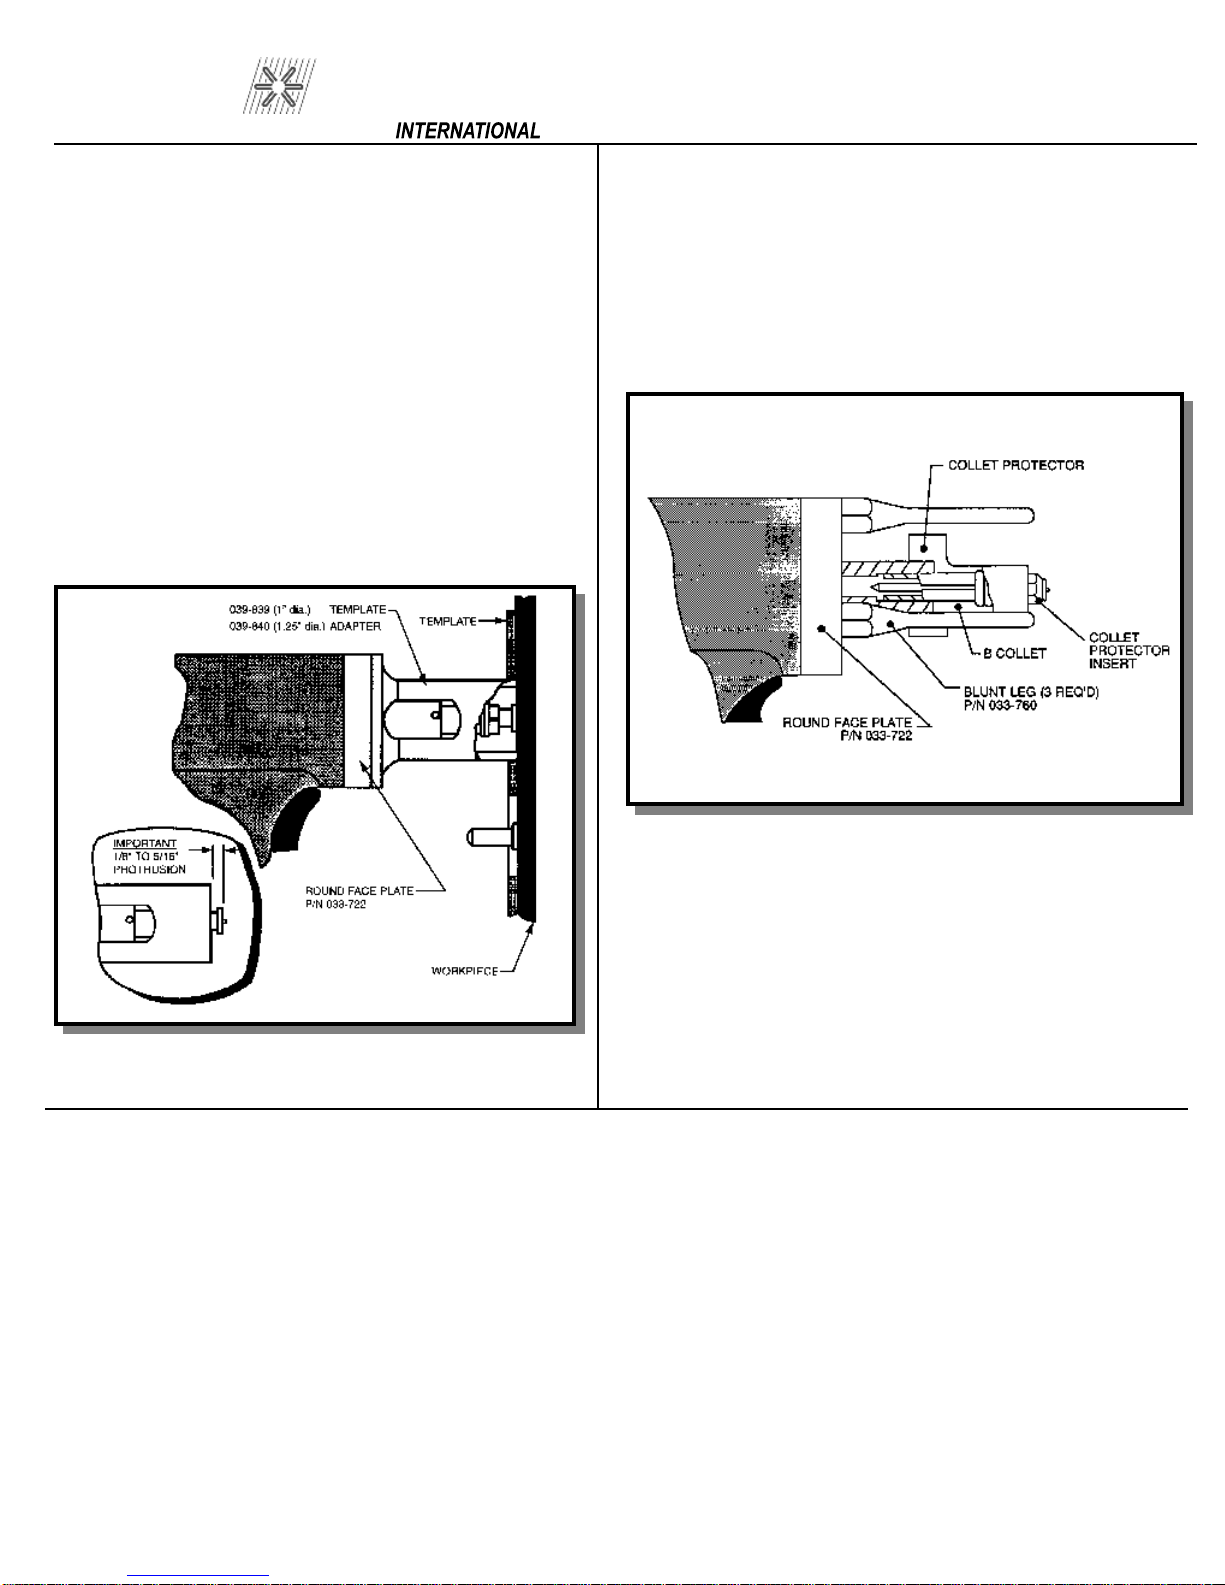
1.4 TEMPLATE ADAPTER (see Figure 7)
The template adapter is used when precise
location or positioning of the CD stud is requir
It is used with the round faceplate and does not r
quire a footpiece or legs. The adapter is fastened to
the faceplate and provides a fixed distance b
tween the collet and work. The plunge is set by u
ing the correct stop in the collet. A template can
then be fabricated to enable very precise locating
of a particular stud.
The template adapter is available in two
sizes, (1” and 1-1/4” diameter).
ed.
e-
e-
s-
CD-512
1
1.5 COLLET PROTECTOR/BLUNT LEG
nately be used with the collet protector as shown in
Figure 8.
(see Figure 8)
The round faceplate, with blunt legs, can alte
r-
Figure 8 Template Adapter gun setup
Figure 9 Collet Protector/Blunt Leg Setup
PAGE 10
Page 19
PRO WELD
CD-512
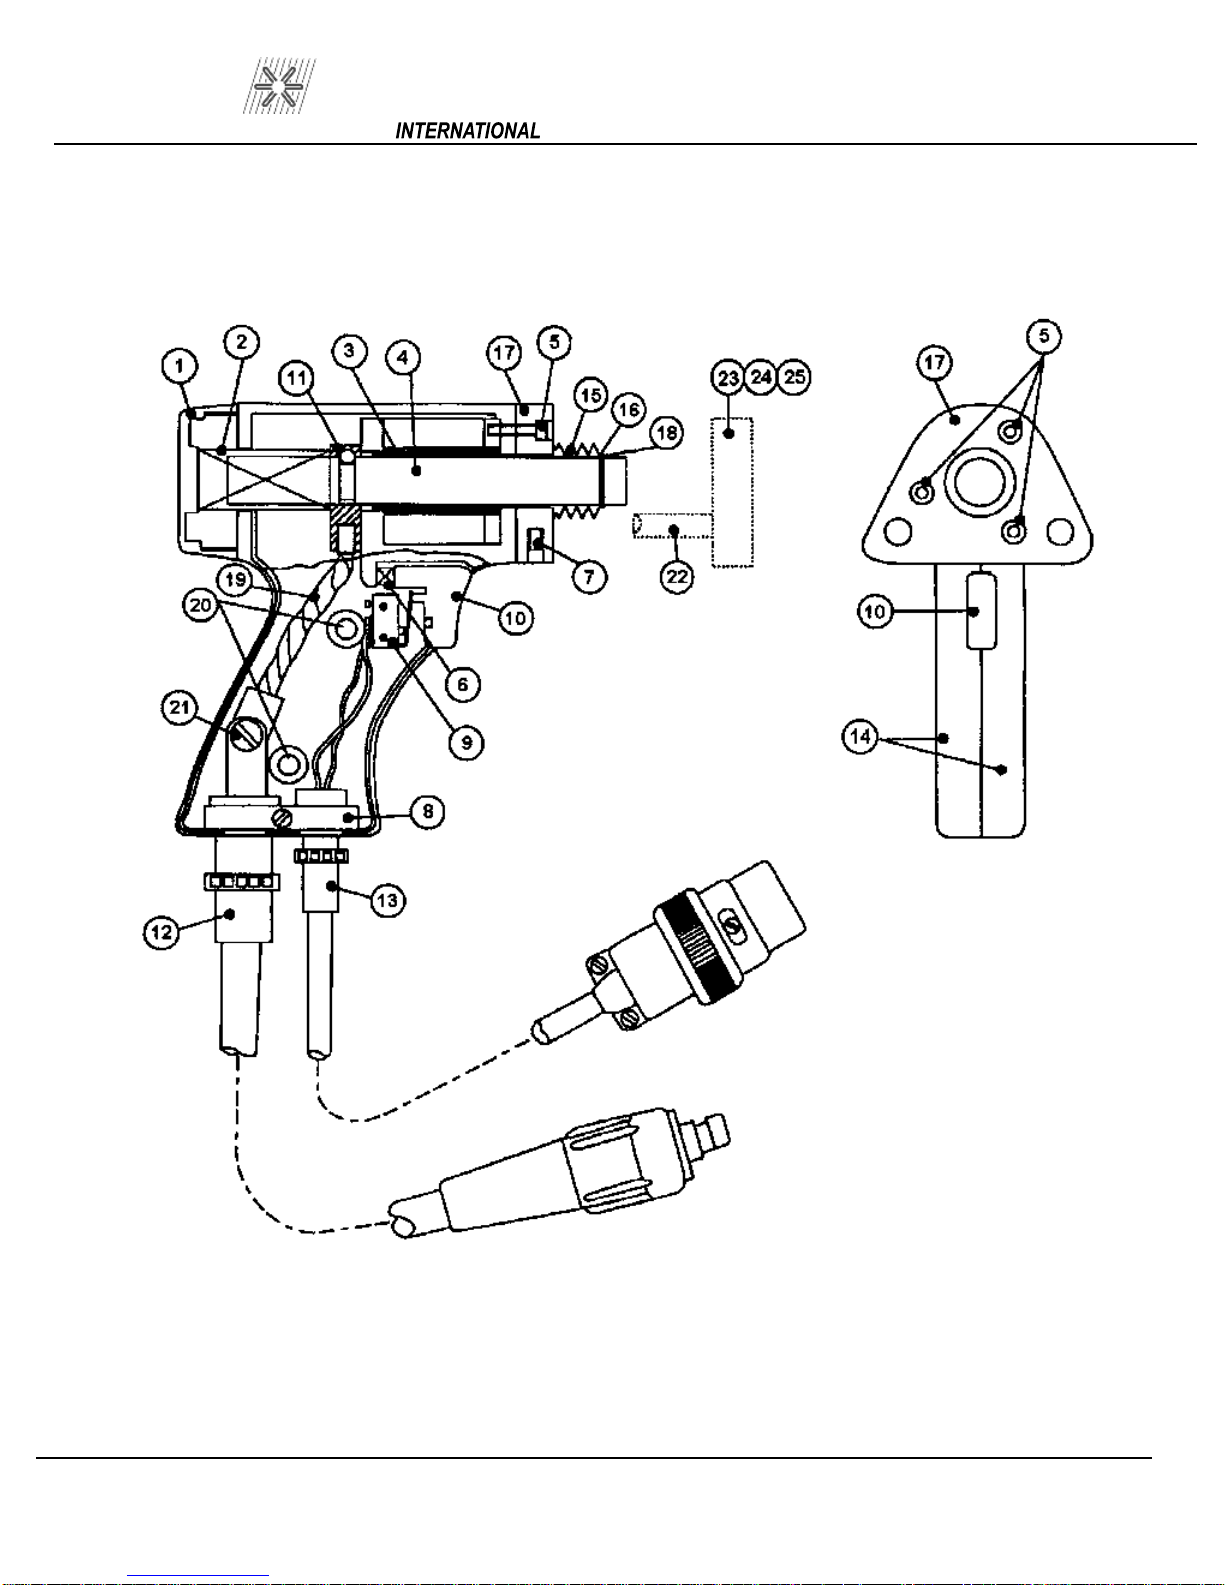
Figure 10 Heavy Duty CD Gun
PAGE 11
Page 20
PRO WELD
11.6 PARTS LIST LIGHT DUTY CD HANDGUN
Part No. 300-0100
ITEM
PART NO.
DESCRIPTION
CD-512
QTY
1 033-384
2 001-801
3 033-610
4 033-799
5 033-016
6 033-382
7 049-955
8
9 033-404
10 033-381
11
12
13
14 033-881
NOT USED
036-496HD
033-662-25HD
033-658-25
GUN CONTROL CABLE (25 FT.) 1
GUN (CD) REAR CAP MOLDED 1
SPRING MAIN HEAVY BLACK
GUN (CD/DA) BEARING ASSEMBLY
GUN (CD) SHAFT TUBE
HEX HEAD CAP SCREW
GUN (CD/DA/FA) TRIGGER SPRING
M SCR
GUN (CD/DA/FA) CABLE CLAMP (ALUM. BLOCK)
TRIGGER SWITCH
GUN (CD/DA/FA) TRIGGER BUTTON MOLDED
GUN (FL) SHAFT BLOCK – A
GUN WELD CABLE (25 FT.)
GUN BODY RH & LH STD.CD MACHINED
EW SET MS, BRASS PLT
1
3
1
1
1
1
2
1
1
1
1
1
15 033-445
16 033-447
17 033-665
18 033-446
19
20 018-375
21 016-876
22 033-757
23 009-929
24 016-378
25 028-833
033-608-HD
PAGE 12
GUN (CD/FL) SHAFT BOOT ASSY
GUN (CD) SHAFT BOOT RETAINING RING
GUN (CD) FACEPLATE – STD. ADJUSTABLE
GUN (CD) SHAFT BOOT SNAP RING
GUN (CD) WELD PIGTAIL A
SCREW PAN HEAD
WASHED, LOCK INTO. TOOTH
LEG (CD) STD.ADJ
FLAT WASHER
SOCKET HEAD CAP SCREW
STD.
FOOTPIECE
2
. 7”
1
1
1
SSY
1
1
1
2 REF.
2 REF.
2 REF.
1 REF.
Page 21
PRO WELD
CD-512
12.0 WELDABLE MATERIAL COMBINATIONS
Structural Steel (
Aluminum – Most alloys of the
1100, 3000 and 5000 series.
Zinc All
BASE MATERIAL
Mild Steel (1008-1018)
Galvanized Sheet (duct-”Q” Decking
Must Be Clean
oys (Die Cast)
)
STUD MATERIALS
Mild Steel 1008, 1018
Stainless Steel 304, 305
Brass 65
Copper, Silicon/Bronze
Mild Steel 1008
Stainless Steel 304,305
Mild Steel 1008,1018
Stainless Stee
Brass 65
Aluminum 1100,5356
Aluminum 1100, 5356
-35, 70-30
-35, 70-30
-1018
l 304,305
Medium Carbon Steel (1030-1018)
Lead Free Brass
Lead Free Rolled Brass
Elec
trolytic Copper
Mild Steel 1008, 1018
Stainless Steel 304,305
Brass 65
Mild Steel 1008, 1018
Stainless Steel 304, 305
Copper, Silicon/Bronze
-35, 70-30
PAGE 13
Page 22
PRO WELD
1
3.0 CAUSE OF POOR OR ERRATIC
WELDS
CD-512
12. Incorrect spring. (REPLACE WITH PROPER
SPRING)
1. Loose collet. Does not grip stud tightly.
(REPLACE) Not enough engagement of stud to co
let. (CHANGE STOP)
2. Fault or loose ground connection. (REPAIR OR
TIGHTEN)
3. Poor surface condition of base material, excess
oil, grease, rust, ect. (CLEAN)
4. Voltage or capacitance setting too low or too high.
(ADJUST TO DIAMETER OF STUD)
5. Broken or loose cables. (REPAIR)
6. Dirt in gun. (CLEAN)
7. Incorrect polarity. (CABLES HOOKED-UP
WRONG)
8. Use of center punch
USE CENTER PUNCH OR DEEP SCRIBES)
or deep scribe. (DO NOT
l-
ive
13. Poor stud quality.
14.0 TROUBLE SHOOTING POOR
WELDS
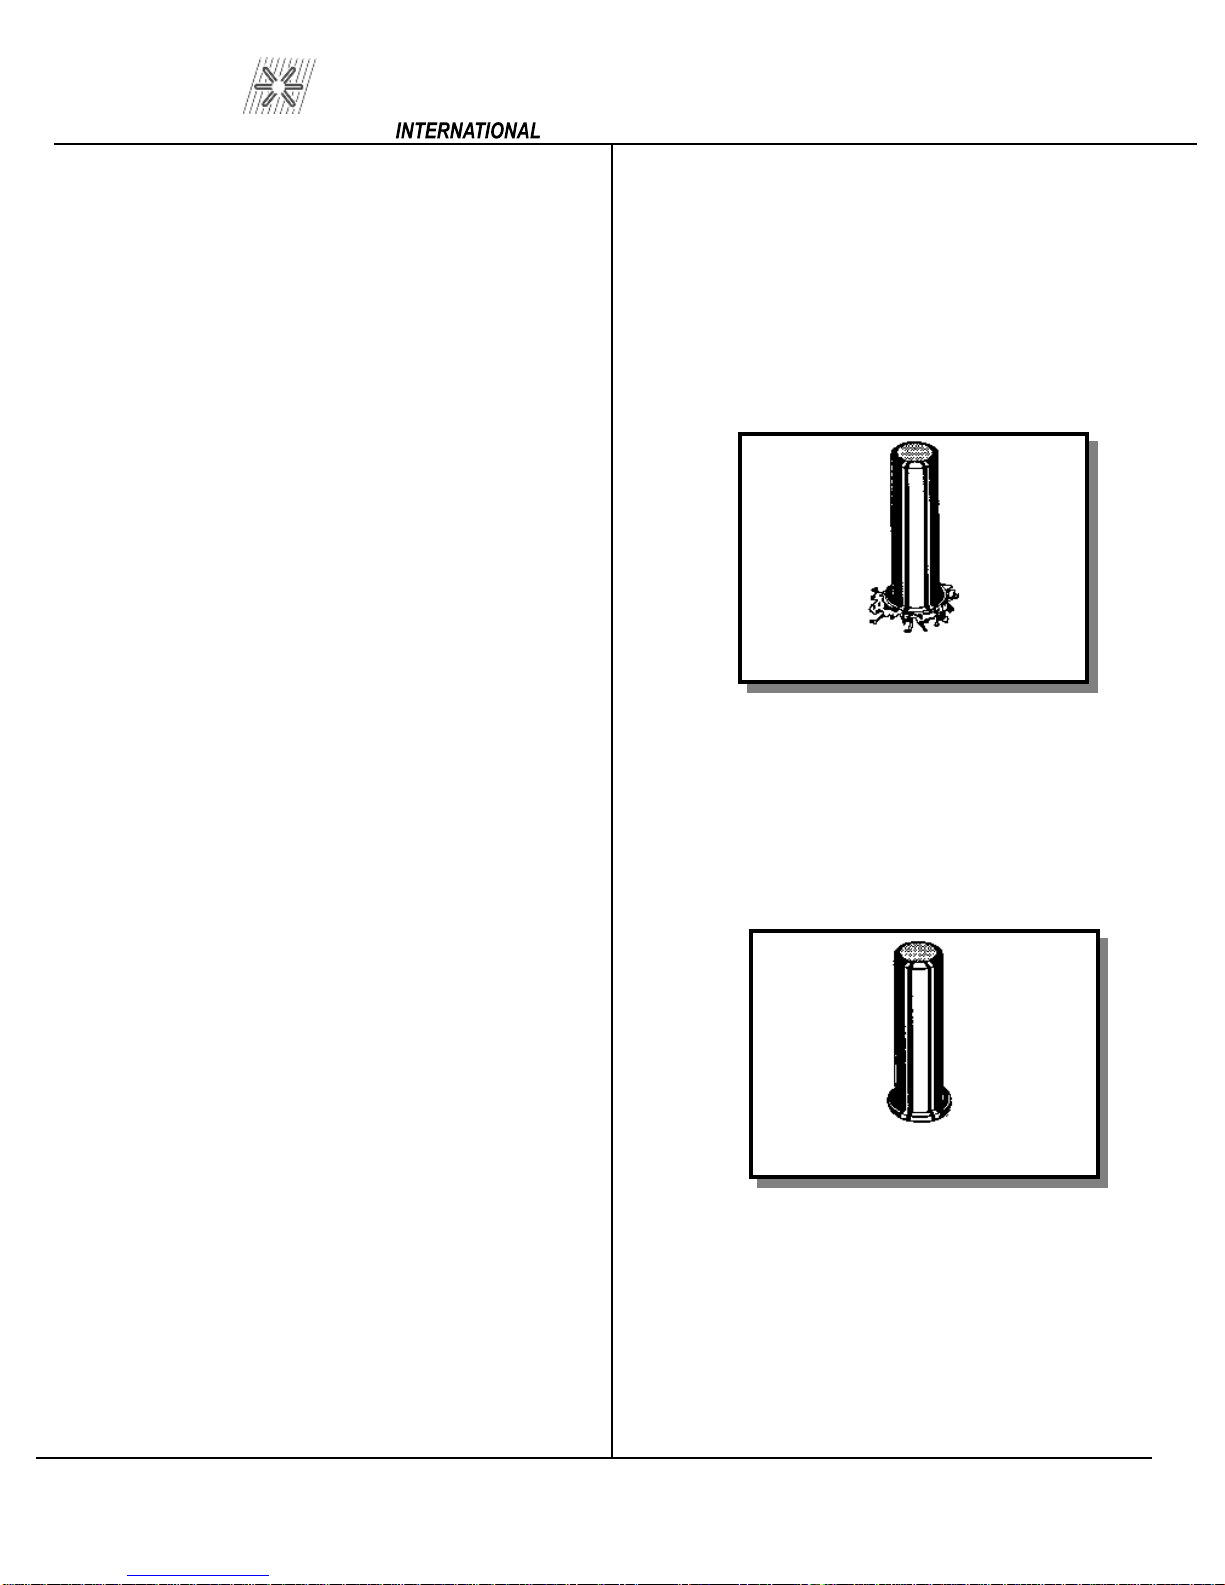
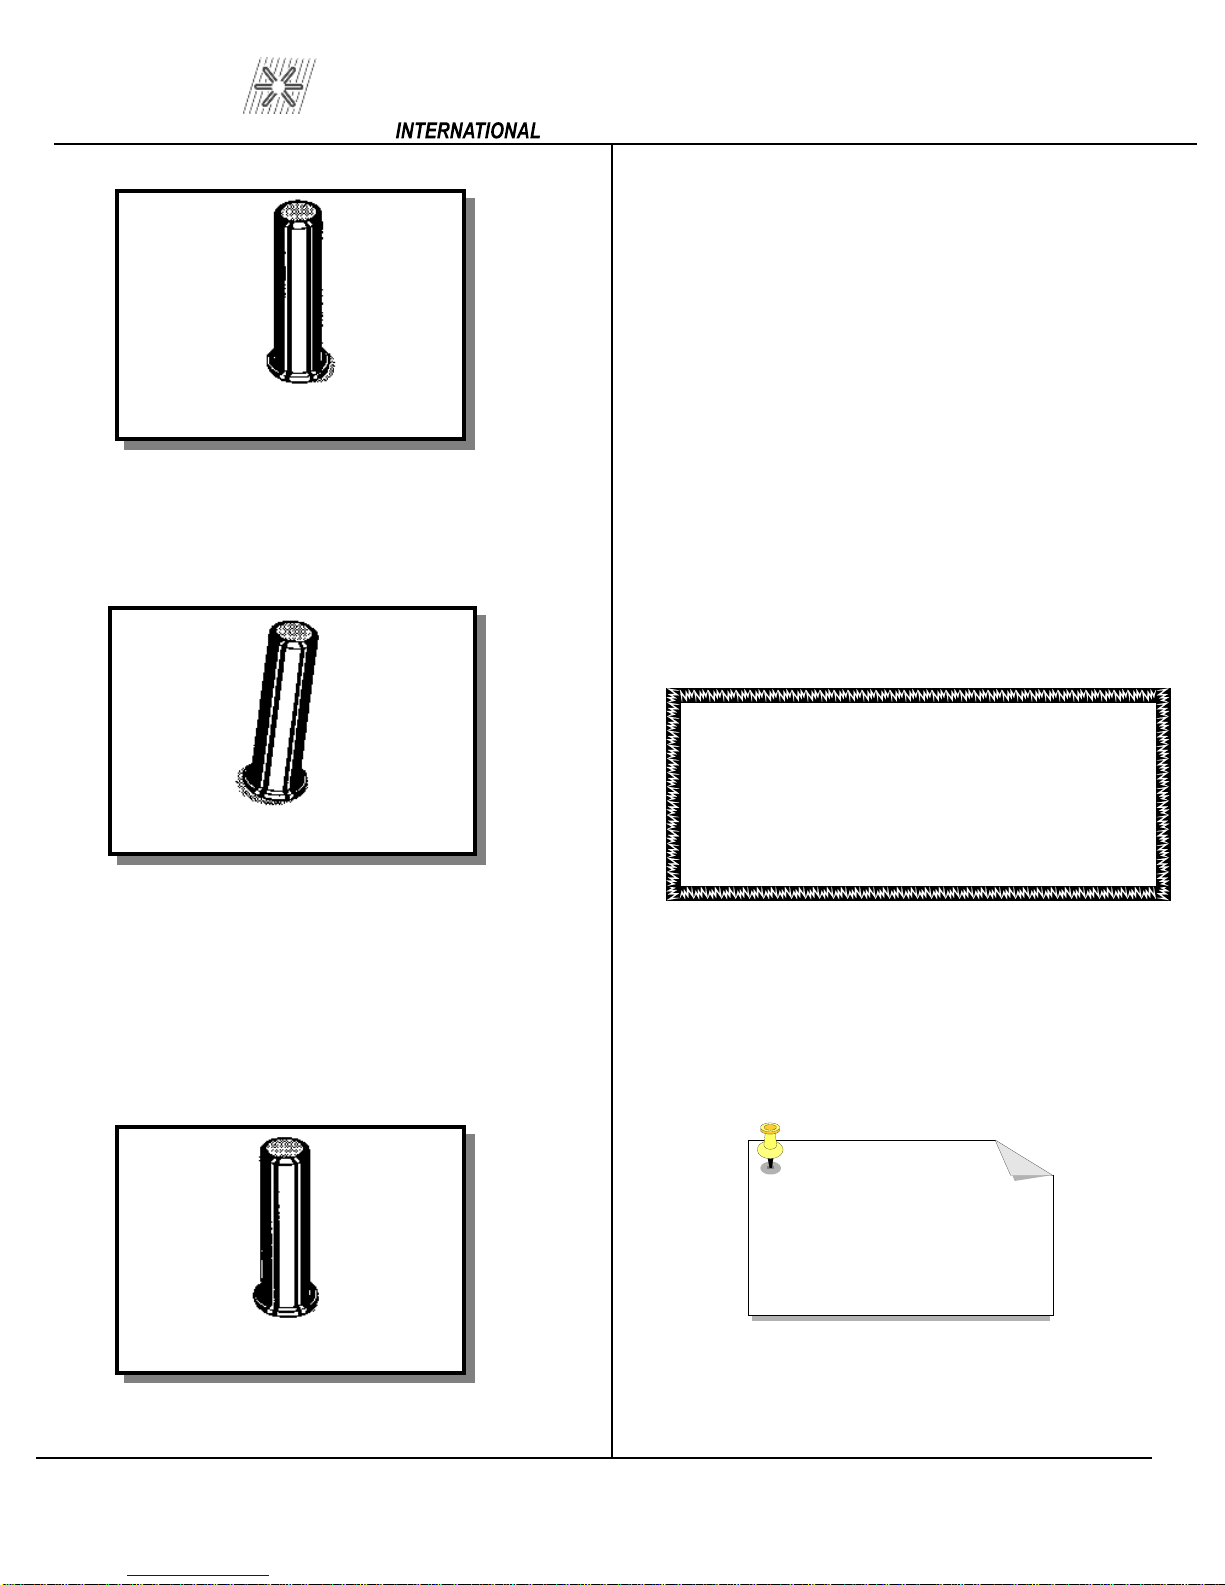
Figure 11 Weld too Hot
Weld too Hot
A) Decrease voltage.
B) Decrease capacitance.
C) Increase stud protrusion.
D) Increase spring pressure.
9. Cables too closely coiled.
10. Arc blow is evidenced by “one side
severe cases there will be no melting under one edge
of flange while the opposite side is gouged out or
appears exce
blow is magnetic field induced by the current flow
during the weld. It occurs most often on long, na
row strips of metal or near edges of sheets or plates.
In some cases, a change in grounding positions, or
two grounds on the wor
edge of work, will correct the problem. For assi
tance in severe cases, contact your local sales repr
sentative.
11. Incorrect plunge setting. (ADJUST TO PROPER
SETTING)
ssively hot. The principle cause of arc
” welds. In
r-
k piece, one at each end or
s-
e-
Figure 12 Weld too Cold
Weld too Cold
A) Increase voltage.
B) Increase capacitance.
C) Decrease stud protrusion.
D) Decrease spring pressure.
PAGE 14
Page 23
PRO WELD
CD-512
1
5.0 ROUTINE WELDER
MAINTENANCE
with minimum care. Ordinary common sense maint
nance will keep it operating efficiently.
Your CD-312 is designed for long service
e-
Figure 13 Arc Blow
Arc Blow
A) Use double grounds.
B) Ground too close or not spaced
Figure 14 Weld without footpiece
Weld without footpiece
A) Use standard footpiece.
B) Use template adapter.
C) Use tripod blunt legs.
bles with respect. Avoid sharp bends and kinks which
may break the cables. Don’t use the cables as a “tow
line” to move the cont
the cables where they enter the gun or at the conne
tors.
the cover of the controller and clean with air and a
soft brush around the
3.
weld cable connections and make sure all the screws
on the capacitor terminals are t
pounds.
1. Treat the welding, ground, and control c
rol. Avoid damage or straining
2. It is good practice to occasionally remove
components.
CAUTION
Be sure the controller is disconnected
from the power before removing the pro
tective cover.
While the cover is removed, tighten all the
orque to 30 inch
a-
c-
-
-
Figure 15 Good Weld
NOTE:
Keep the gun free of
dust, dirt or foreign
material
PAGE 15
Page 24
PRO WELD
CD-512
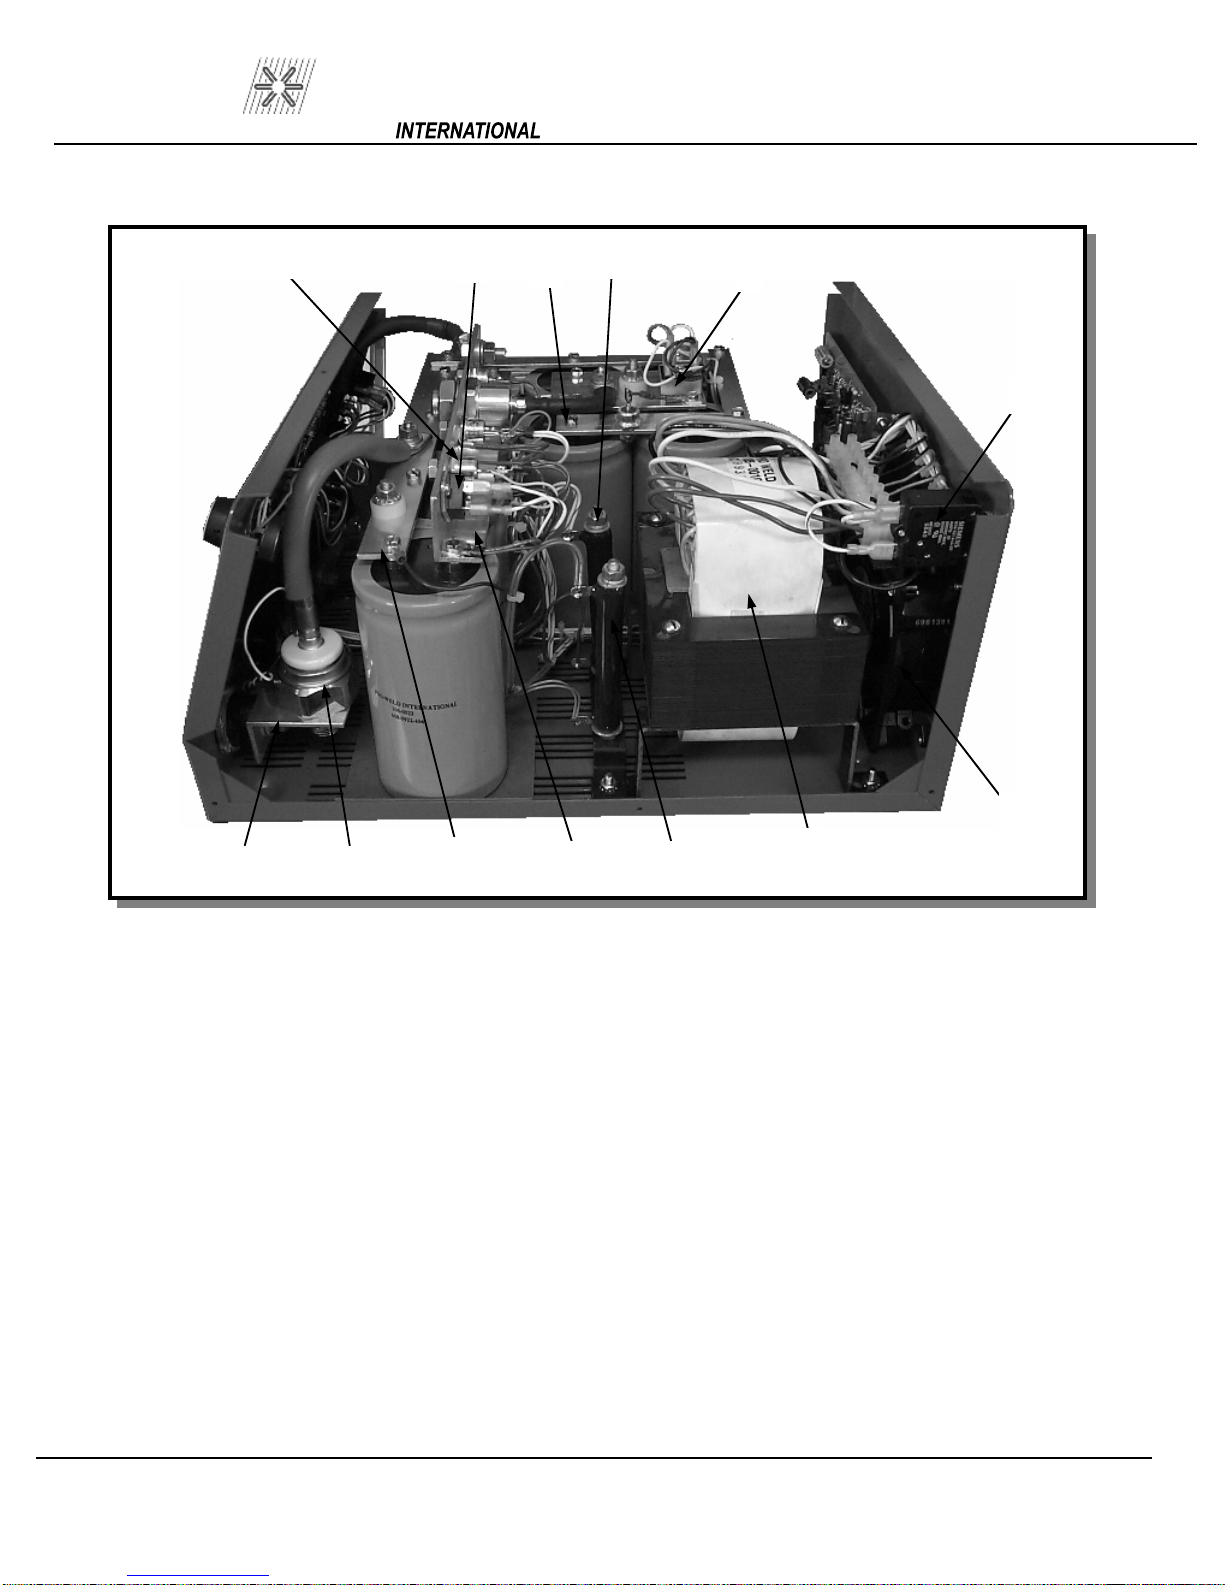
16.0 ASSEMBLY CD-512 CONTROLLER
13
12
11
10
(see Figure 15,16, & 17)
9
8
1 2
ITEM
1 SCR Mounting 124-0026
2
3
4
5
6
7 Fan 102-0014
8
9
10
11
12
13
3
Figure 16 Parts List
DESCRIPTION
Main SCR
Buss Bar
Buss Bar
Dropping Resistor
Transformer
Circuit Breaker
Charge Bridge
Discharge Resistor
Buss Bar
Safety SCR
Charge SCR
4 5
108-0001
124-0043
124-0038
112-0042
105-0010
104-0021
108-0017
112-0041
124-0040
108-0042
108-0002
6
PART NUMBER
7
PAGE 16
Page 25
PRO WELD
20
CD-512
14
16
15
ITEM
14
15
16
17
18
19
20
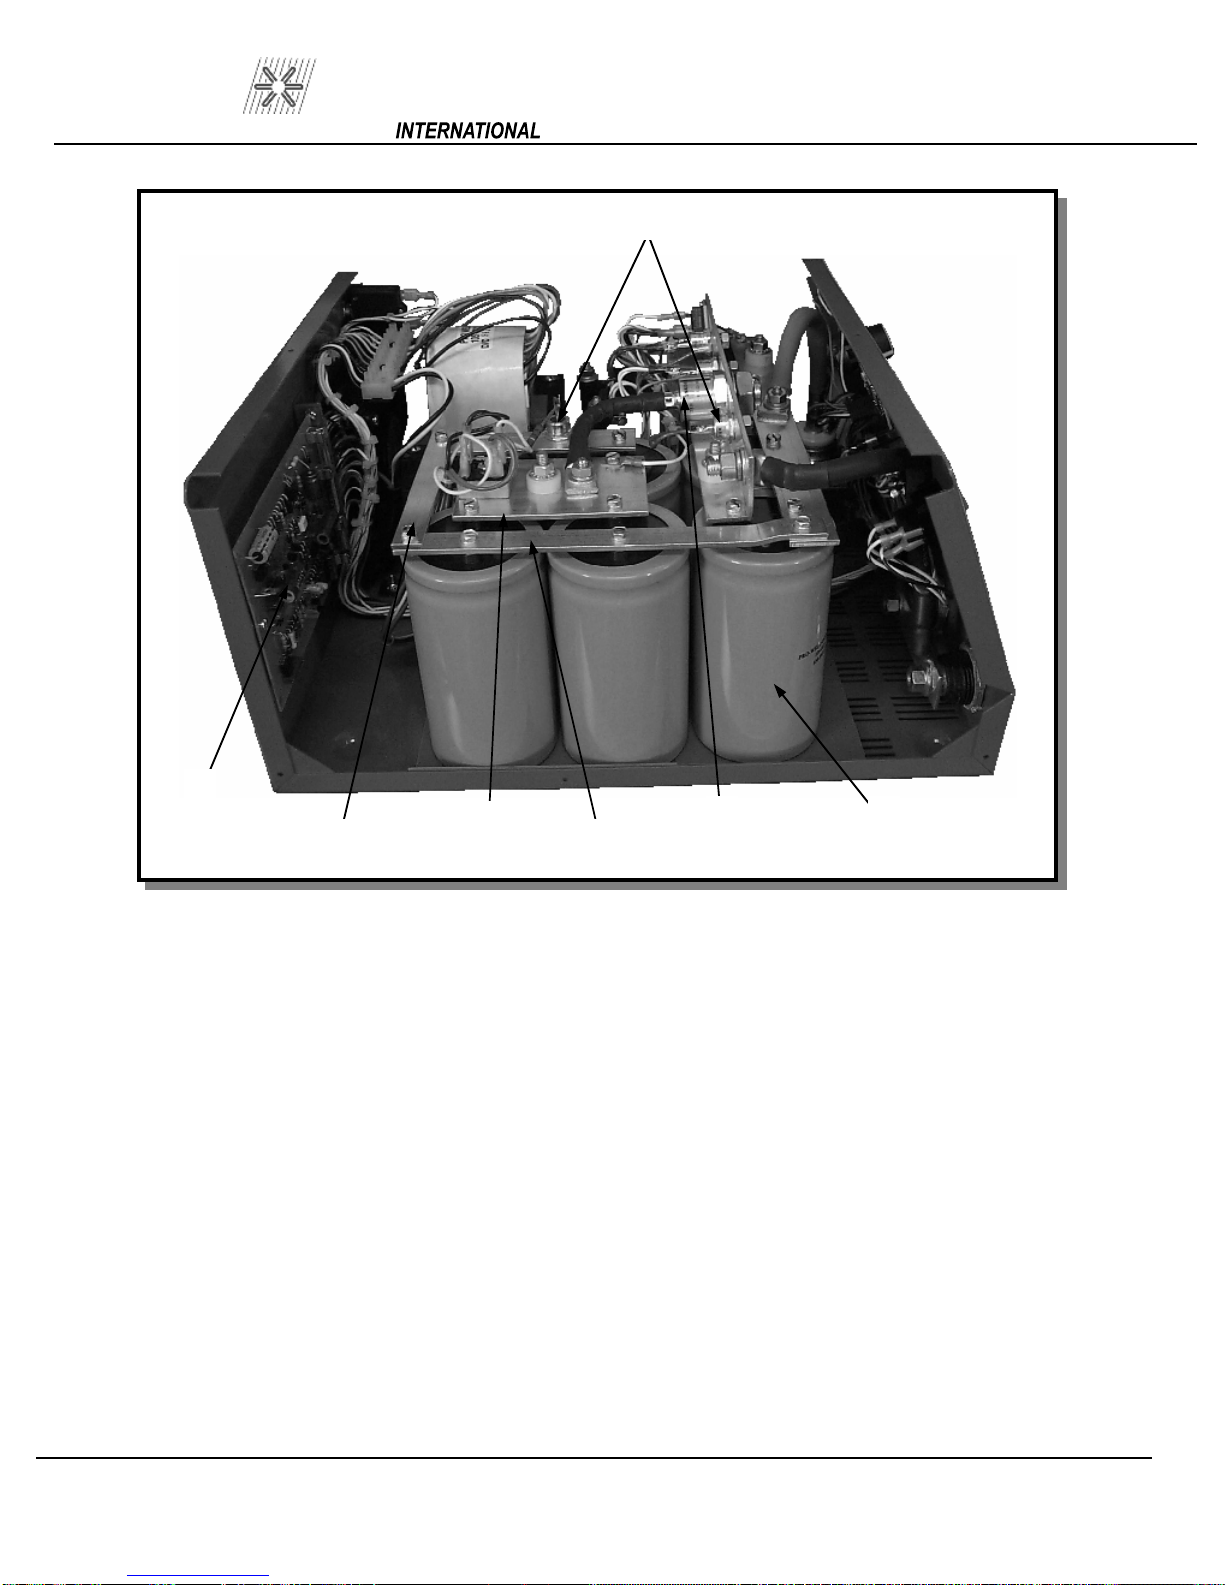
Figure 17 Parts List
18
17
DESCRIPTION
PC Board
Buss Bar
Buss Bar
Buss Bar
Diode
Capacitor (8)
Diode
600-0007
124-0042
124-0041
124-0039
108-0005
108-0027
106-0001
PART NUMBER
19
PAGE 17
Page 26
PRO WELD
26
28
29
27
25
CD-512
24
23
22
21
Figure 18 Parts List
ITEM
21
DESCRIPTION
Female Camlok (3)
22 223
LED Amber (Contact)
107-0002
Pole Female Hubble
107-0031
108-0030
PART NUMBER
24 Knob 102-0060
25
26 High27
28
29
LED Panel Meter
103-0002
Low Range Switch
Power Switch
104-0013
LED Green (Ready)
LED Red (Trigger)
104-0014
108-0029
108-0028
PAGE 18
Page 27
PRO WELD
CD-512
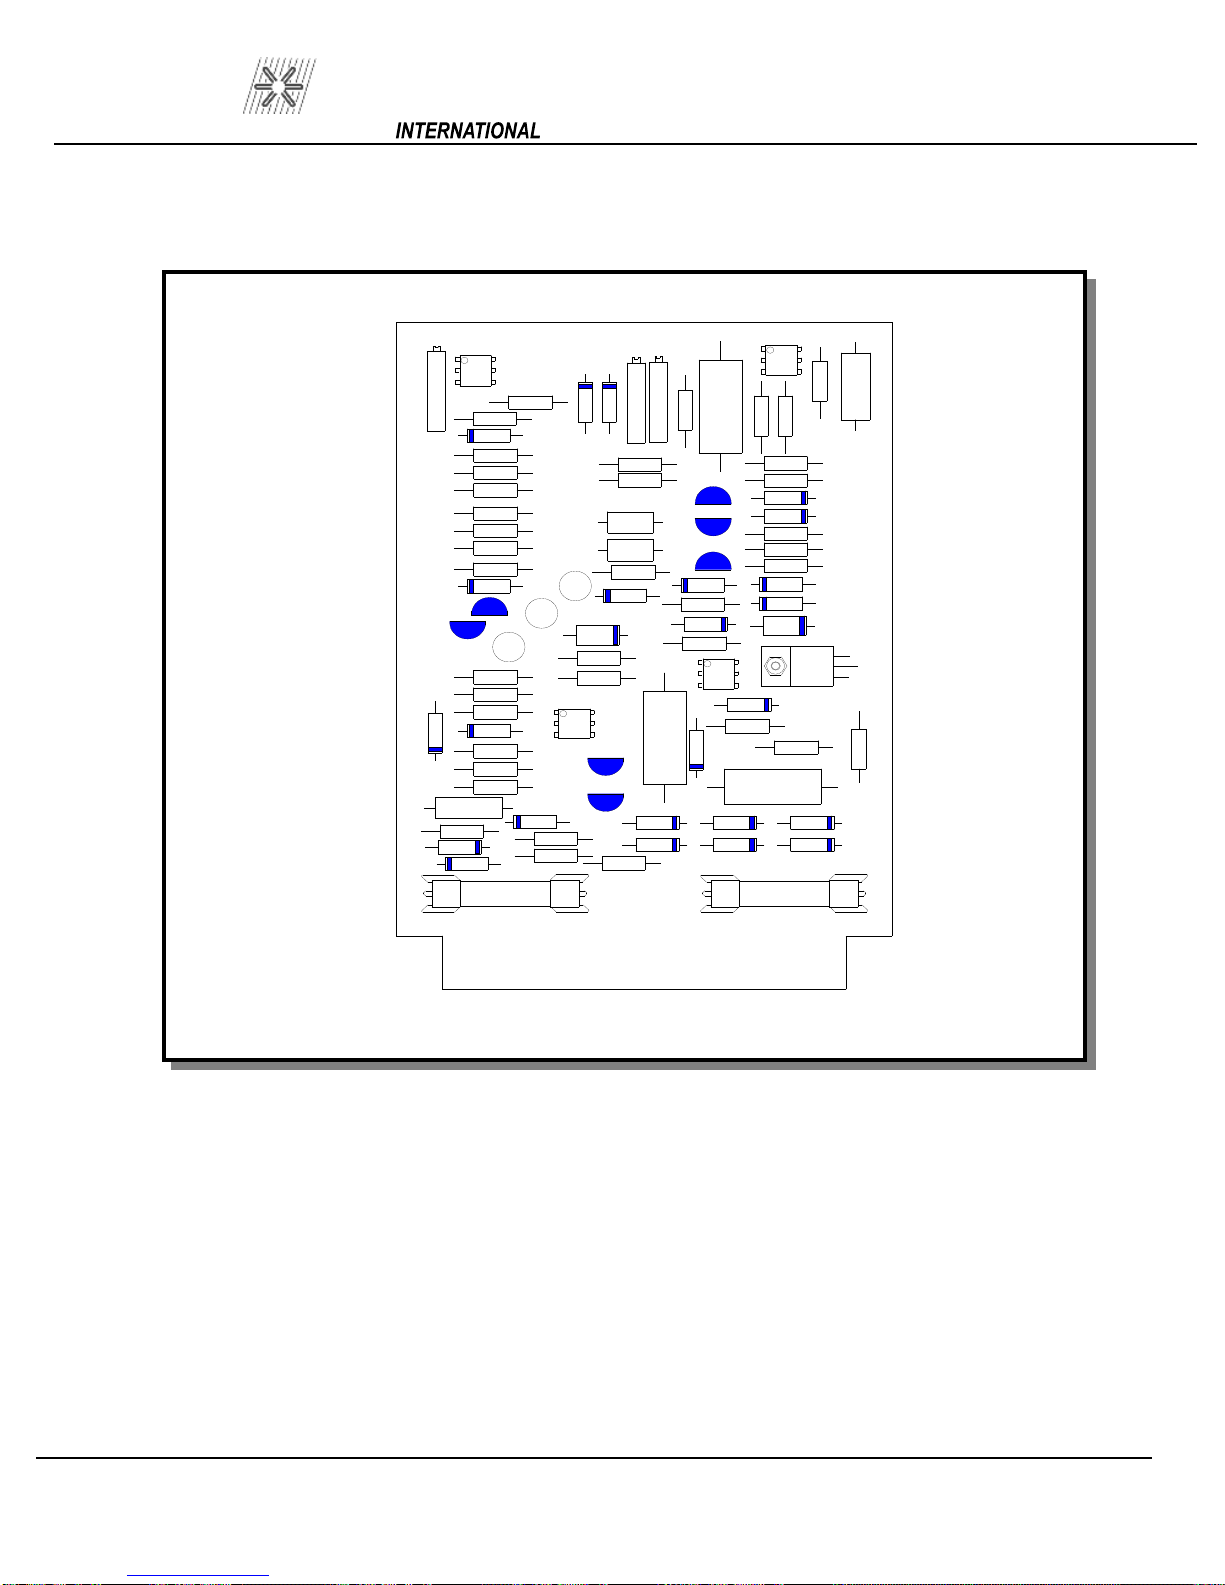
16.1 PC BOARD ASSEMBLY DRAWING
FU2 and FU3 are 3AG 1 ampere fuses
OP1
R24
R34
D11
R30
R25
R17
R16
R18
R28
R27
D10
V5
V4
R20
R26
R19
D14
D13
R23
R40
R37
+
C9
R36
D21
D16
C6
FU2
+
R44
D23
+
C4
R41
R22
+
V7
V6
C5
OP3
OP4
R33
R13
V2
V1
R10
R43
R29
R7
OP2
D18
R15
D7
D6
R3
R1
R2
D8
ZD2
ZD1
D9
R8
R39
C7
D20
D19
FU3
V3
D2
R5
D1
R9
D3
R14
R4
D5
D4
R12
R11
C1 C2
R31
ZD4
ZD3
R6
R32
ZD5
D22 D17
R35
VR1
+
R42
+
C3
R38
Figure 19 PC Board
PAGE 19
Page 28
PRO WELD
CD-512
17.0 TROUBLE SHOOTING – ELECTRICAL
When troubleshooting the power unit/controller (welder), the following precautions must be
1. Welder must be TURNED OFF!
2. Unplug power cable from welder and wait at least two minutes before checking compo
3. The use of a volt/ohmmeter is recommended where any voltage may be present.
4. Use a continuity tester ( or troubles
5. Possible causes marked with a star (*) are generally the most common problems.
P
ROBLEM
1. Welder does not turn on
and
loose wire connection in
the plug.
will not weld.
hooting light) for continuity checks only.
POSSIBLE CAUSE
A. Power connections at
Welder or 110 VAC outlet
not complete.
*B. Broken power cable or
C. Fuse blown.
CORRECTIVE ACTION
Check connections.
Check wires for continu
Repair break.
Replace fuse.
observed:
nents.
ity.
2. Fuse bl
unit is turned on.
ows each time
Rupture hole. Replace
*A. Shorted weld capacitor.
B. Shorted rectifier (BR1)
C. Incorrect primary hookup.
D. Shorted transformer
assembly.
Check safety vent seal for
defective capacitor.
Check for a short across the
rectifier with ohmmet
Replace rectifier module if
shorted.
Check transformer connect
Replace transformer.
er.
ions.
PAGE 20
Page 29
PRO WELD
CD-512
PROBLEM
3. Welder turns on but
does not operate
*B. Broken gun control cable
or loose wire c
in either direction). Replace
4. Weld is excessively hot
regardless of vo
setting.
A. Ground cable connections
ltage
In either direction). Replace
POSSIBLE CAUSE
not complete.
in the plug. Shorted or
open trigger swit
*C. Faulty printed circuit
board.
D. Sh
A. Shorted charge SCR.
orted weld SCR.
onnection
ch.
CORRECTIVE ACTION
Check for continuity
Check continuity between
pins on control plug while
trigger is depressed.
Should read continuity.
Replace with new PC
Board.
Check with ohmmeter
(should not show continuity
rectifier module if shorted.
Check with ohmmeter
( should not show continuity
if shorted.
5. Poor and erratic
welding.
*B.
Faulty printed circuit
board.
C. Open voltage
potentiometer.
A. Improper gun setup.
B. Improper grounding or
cable setup or incorrec
polarity.
C. Weld cables are coiled.
D. Incorrect voltag
E. Studs or pins not
perpendicular to work
surface.
e setting.
t
Replace defective legs.
Replace with new PC
Board.
Replace defective voltage
Potentiometer.
Check applicable gun setup
Instruction page.
Check applicable cable setup
Instruction page.
Straighten out cables.
Adjust as necessary.
Adjust legs as necessary.
PAGE 21
Page 30
PRO WELD
18.0 CHECK LIST CD-512 SYSTEM PT. NO. 100-0110
STANDARD CD-512 WELDING SYSTEM COMPLETE WITH B-COLLET GUN
AND 25’ #2 GROUND CA
ITEM
1. CD-
2.
3.
4. MANUAL, Operation and Maintenance CD-512 1
5.
19.0 CHECK LIST CD-512 SYSTEM PT. NO. 100-0111
DESCRIPTION
512 CONTROLLER 110 VAC
GUN ASSY. B-COLLET w/INTEGRAL 2
& CONTROL CABLE 2-LEGS, and FOOTPIECE
GROUND CABLE #2 X 15’ (2 REQUIRED)
HEX WRENCH SET
BLE
200-0013 1
5 FT.WELD
125-0101 1
1
PART #
300-0200 1
CD-512
QTY
STANDARD CD-512 WELDING SYSTEM COMPLETE WITH TAPER TIP GUN
AND 25’ #2 GROUND CABLE
ITEM
1. CD-
2.
3.
4. MANUAL, Operation and Maintenance CD-512 1
5.
DESCRIPTION
512 CONTROLLER 110 VAC
GUN ASSY. TAPER TIP w/INTEGRAL 25 FT.WELD
& CONTROL CABLE 2-LEGS, and FOOTPIECE
GROUND CABLE #2 X 15’ (2 REQUIRED)
HEX WRENCH SET
PART #
200-0013 1
300-0201 1
125-0100 1
1
QTY
PAGE 22
Page 31
Page 32
MANUFACTURED BY
WELD
PRO
MADE IN THE U.S.A.
 Loading...