

Page 1
Ultra-lightweight indoor and park glider
www.planeprint.com
the ONLY place where you can get
original Planeprint STL fi les legally!
PRINTING & ASSEMBLING MANUAL
Page 2
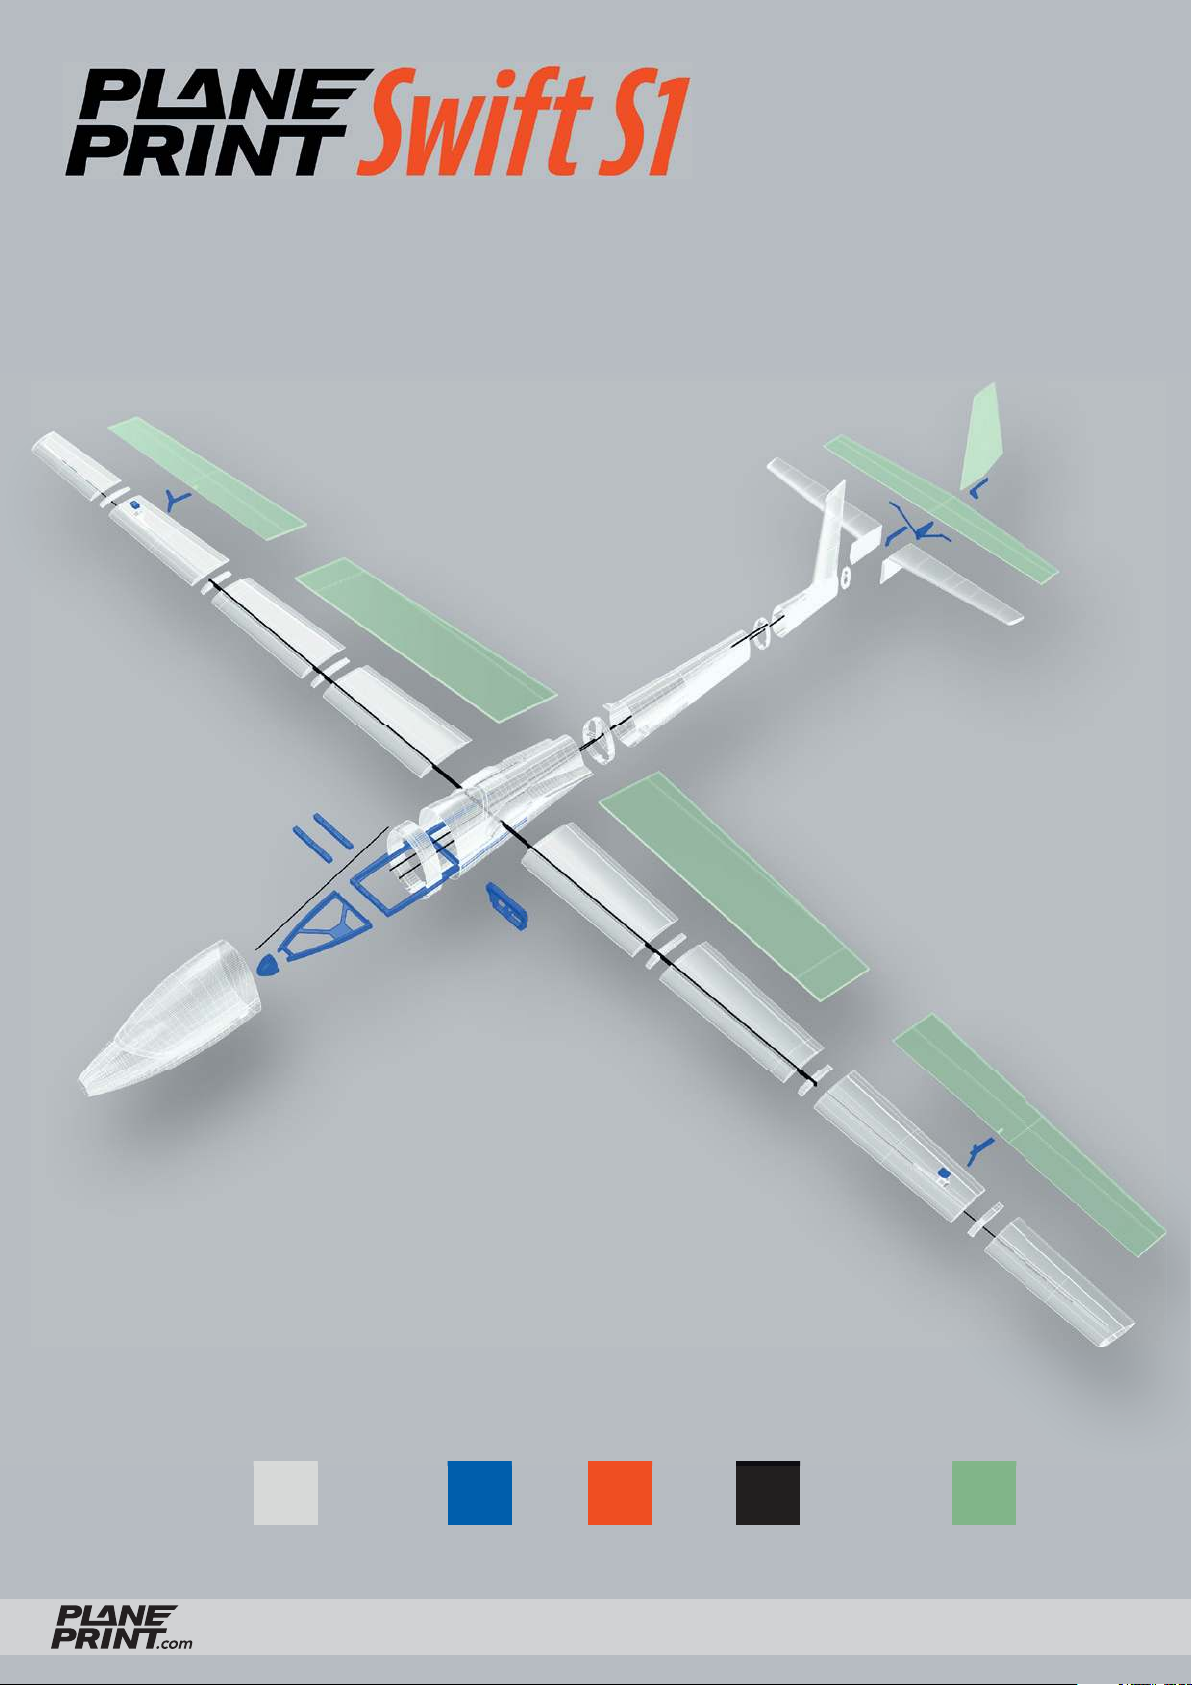
PLALW-PLA TPU FOAMCARBON
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
2
Page 3
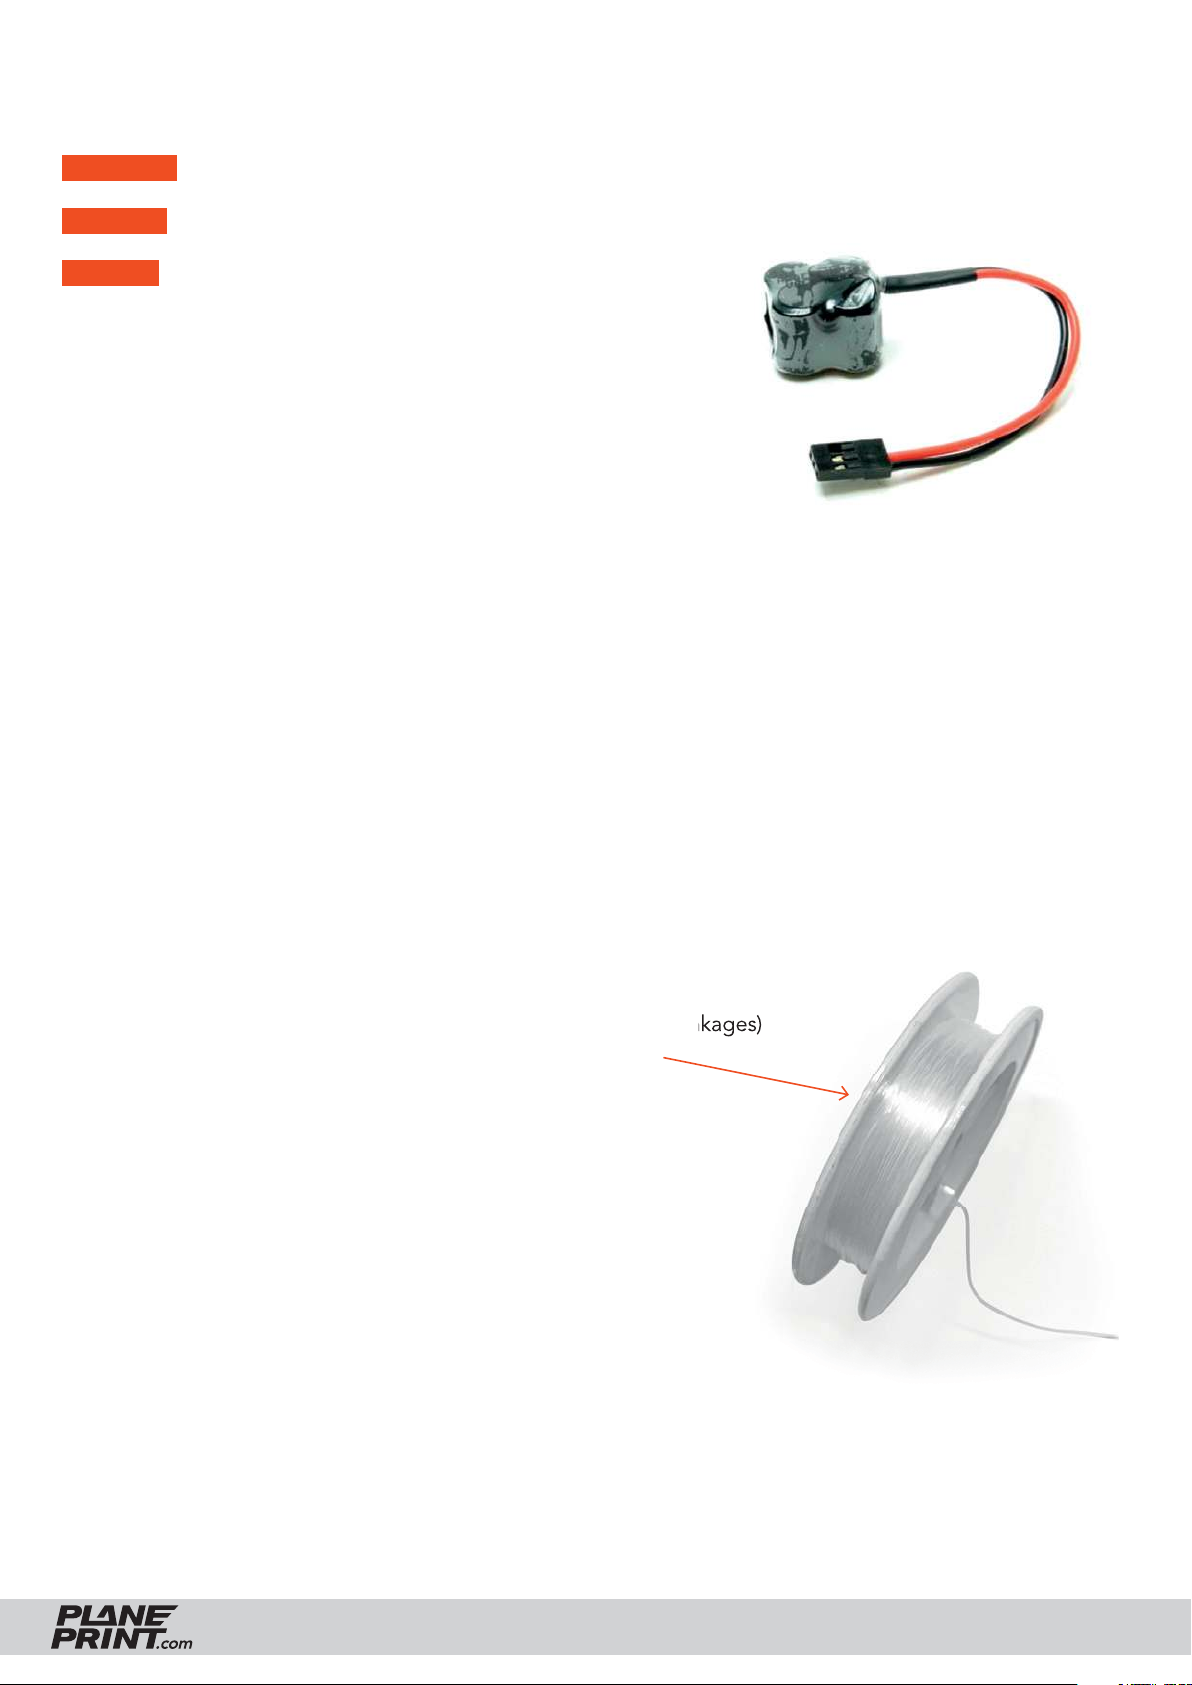
RC Components
RECEIVER 4 Channel (light indoor receiver)
BATTERY Micro Receiver battery (like E-Akku Team Champion 4 Würfel 4.8/150 Graupner SJ – 18 grams)
SERVOS 4 Micro or Nano Servos (3 without Tow Function)
for example: • Hitec HS 40 Eco Servo 4,8g
• Diamond D47
• PLANET-HOBBY ECO PLUS
• Stemedu Micro 3.7g Servo GH-S37D
• PICCO 8 DIGITAL SERVO
Required accessoires
Links to recommended accessories can be found on
www.planeprint.com/swift (scroll down)
• LW-PLA (cannot be replaced by PLA!), ~100 grams
• PLA or Tough PLA, ~20 grams
• CA super glue (liquid and medium)
• CA activator
• Foam board 3 mm uncoated!*
(or Foam like Depron, Styropor or EPP, you can see how much you need on the next page
– Such boards are also available separately in model shops)
• UHU POR glue (or another glue suitable for Depron)
• Carbon rod Ø1*1000mm, 3 pieces
• Carbon fi ber strip (fl at profi le) 1*5*1000mm, 1 piece
• a few short pieces of thin steel wire, approx. Ø0.6 mm (for the linkages)
• thin smooth nylon silk Ø approx. 0.2 to 0.3 mm (Fishing line)
• Adhesive tape
• Self adhesive velcro tape
– basic equipment
* These parts cannot be printed for weight reasons,
LW PLA is much heavier than foam.
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
3
Page 4
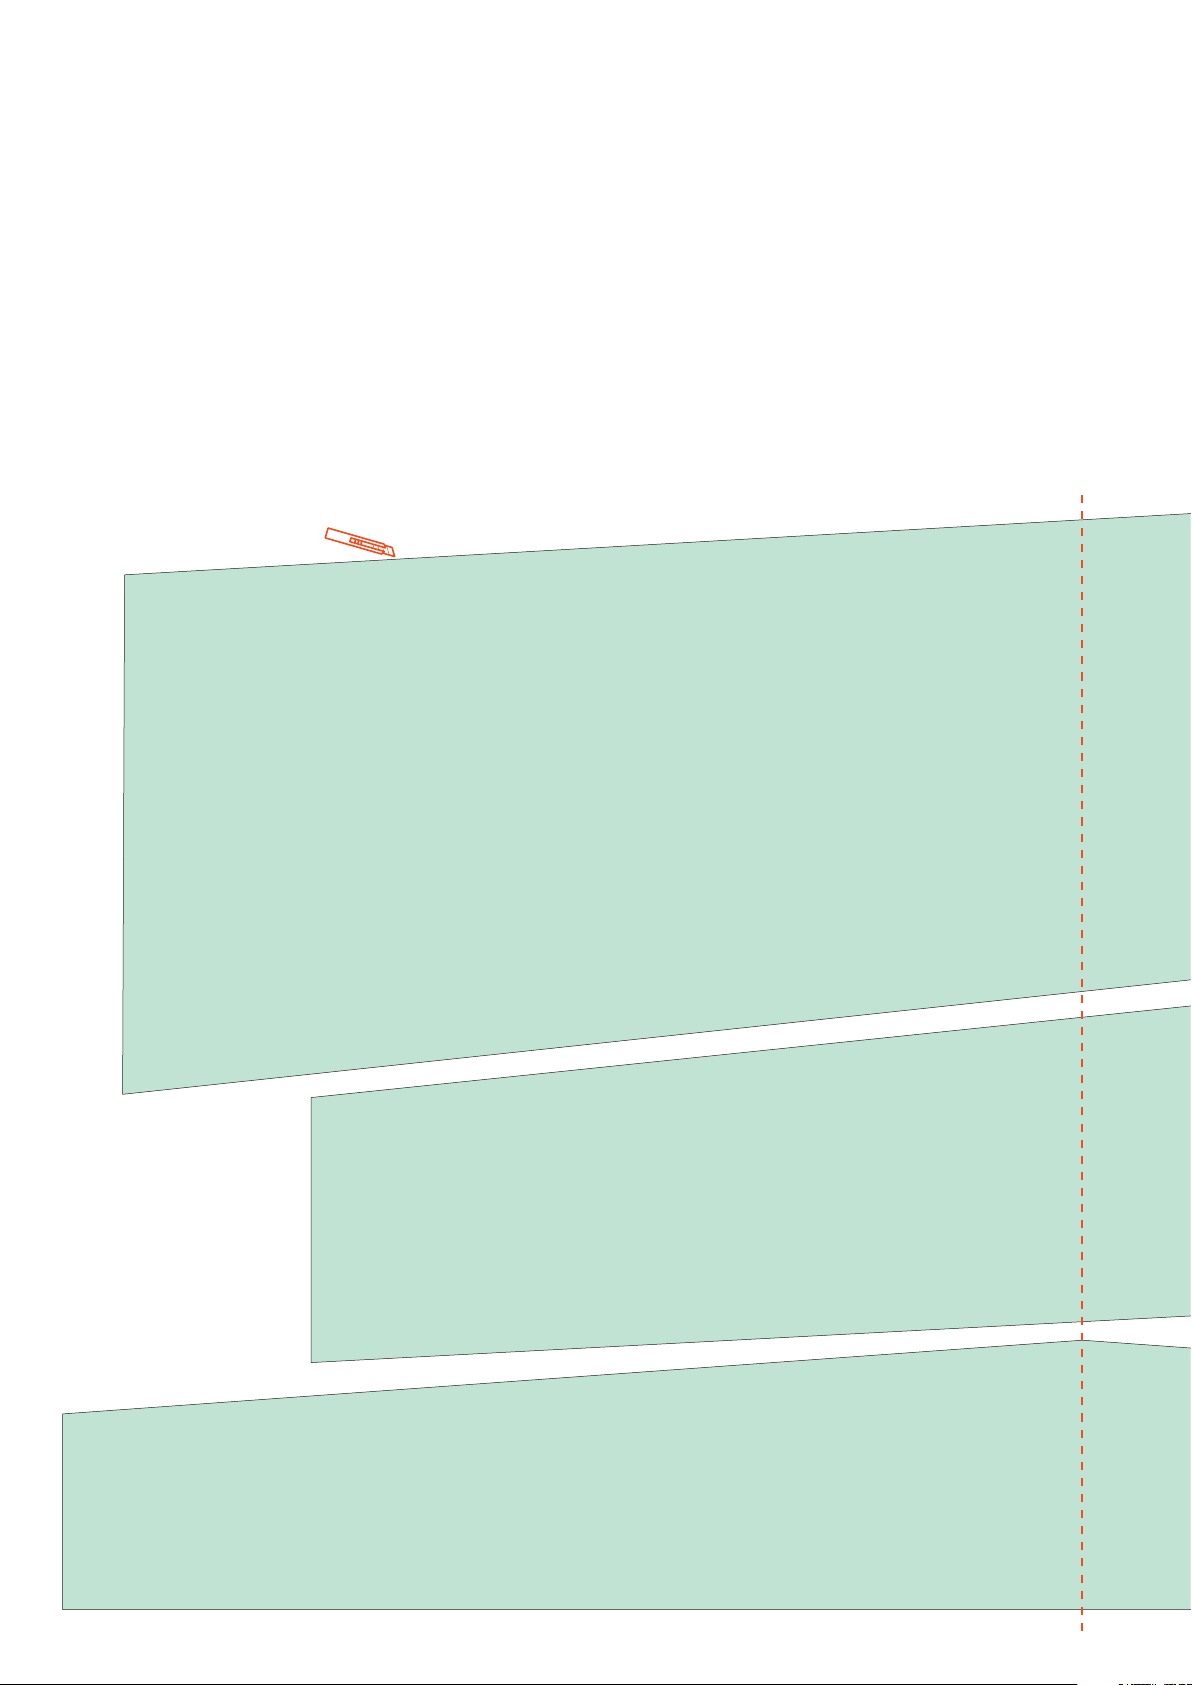
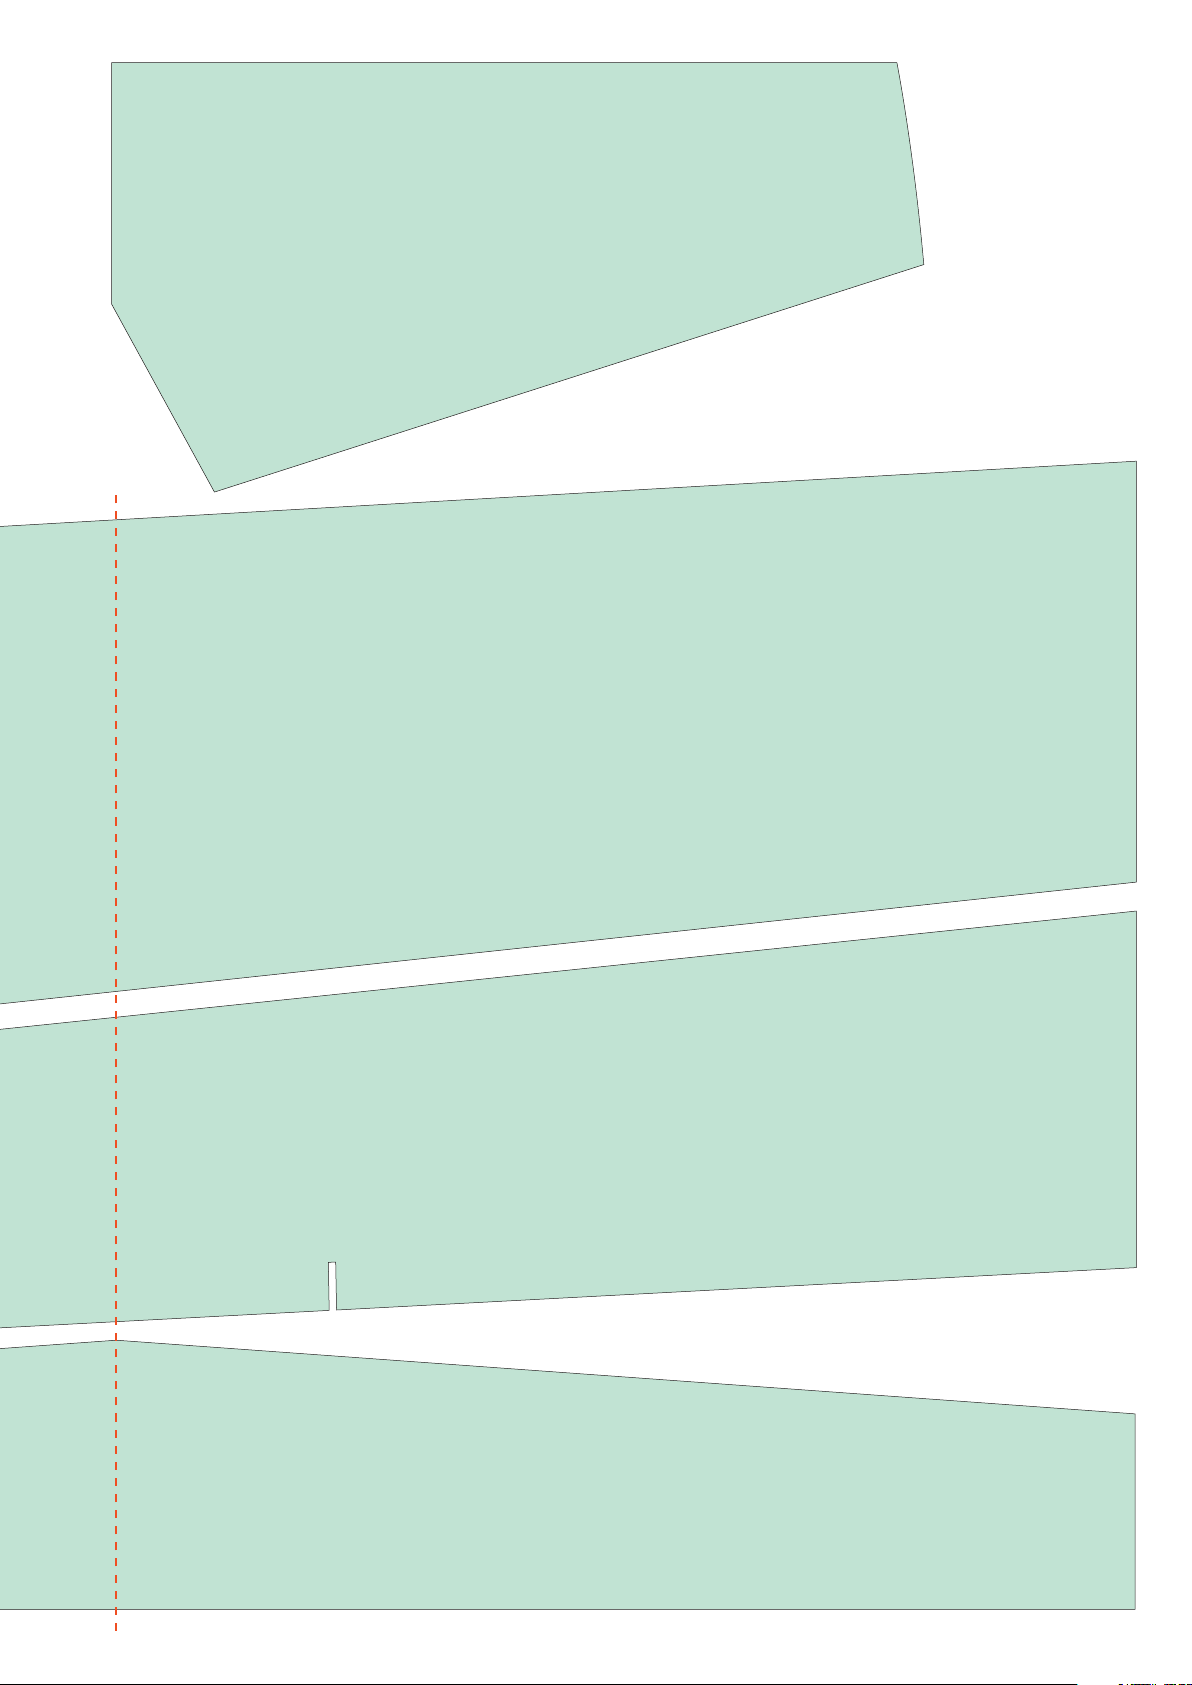
Cutting template for the Depron parts
Print out these two pages on A4 paper, cut them along the red dotted line and tape the
pages together exactly. Then cut out the templates for the wing, ailerons, elevator and
rudder. Fix them to the Depron board and cut two pieces from each (aileron and wing)
and one rudder and elevator.
IMPORTANT: the print must be set to 100% page size, so that the size fits exactly!
Wing part (twice)
Aileron (twice)
Elevator
Page 5
Wing part (twice)
Rudder
Aileron (twice)
Elevator
Page 6
The development of a complex, airworthy RC flight model to express on any standard 3D printer is a very extensive process.
not to forward the STL data you have acquired to third parties.
Thank you for your understanding and have fun with your PLANEPRINT MODEL!
Therefore, we appeal to your fairness
Printing the parts – Printing profiles
This manual is constantly being improved and supplemented, we recommend
downloading the latest version from our website before building.
To print all PLANEPRINT models you need to set some basic profiles in Cura
(If you use another slicer, please set the same parameters).
You can find the description at
For this model you need the following profile:
www.planeprint.com/print
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
6
Page 7
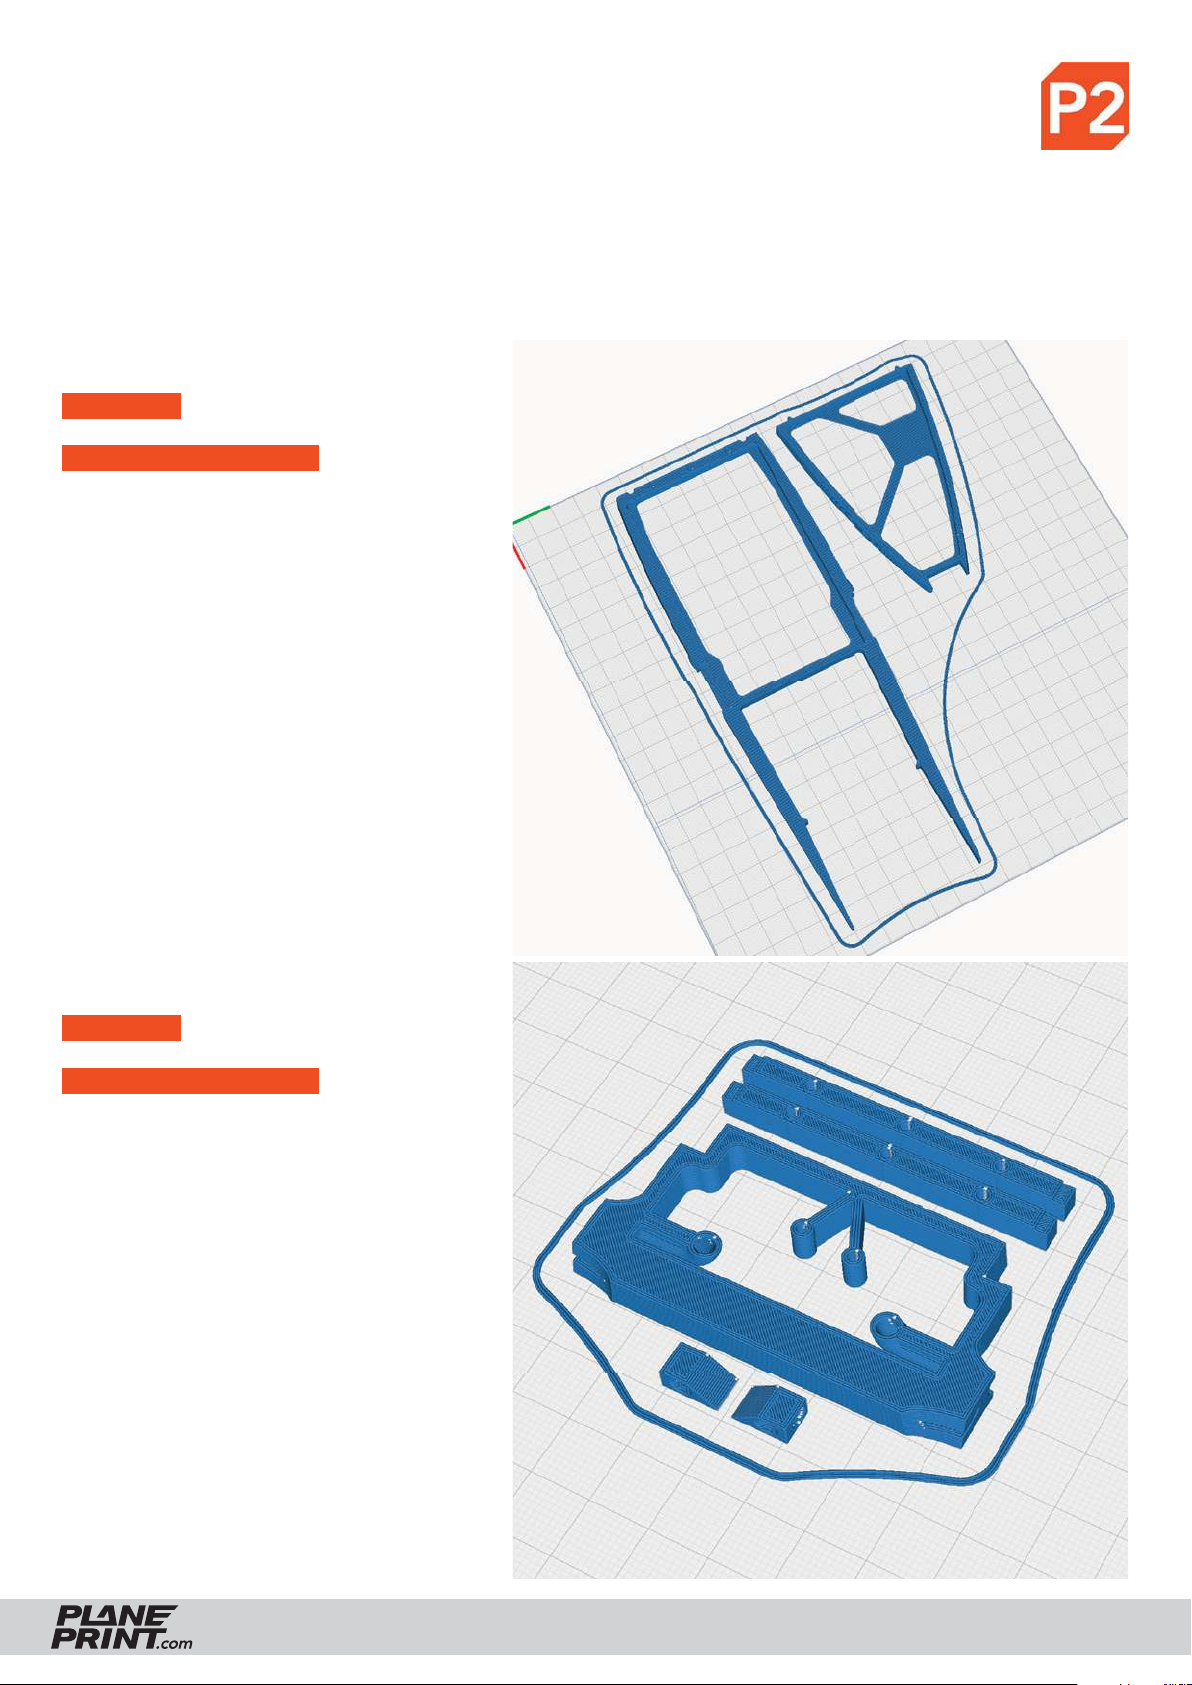
PROFILE P2_Hollowbody PLA or Tough PLA
The information about the basic settings you can fi nd on our website at PRINT.
Please note the additional settings for the individual parts!
P2_Frame–S1.stl
MATERIAL PLA, Weight: ~ 9 g
ADDITIONAL SETTINGS
None required
P2_Parts 1–S1.stl
MATERIAL PLA, Weight: ~ 7 g
ADDITIONAL SETTINGS
None required
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
7
Page 8
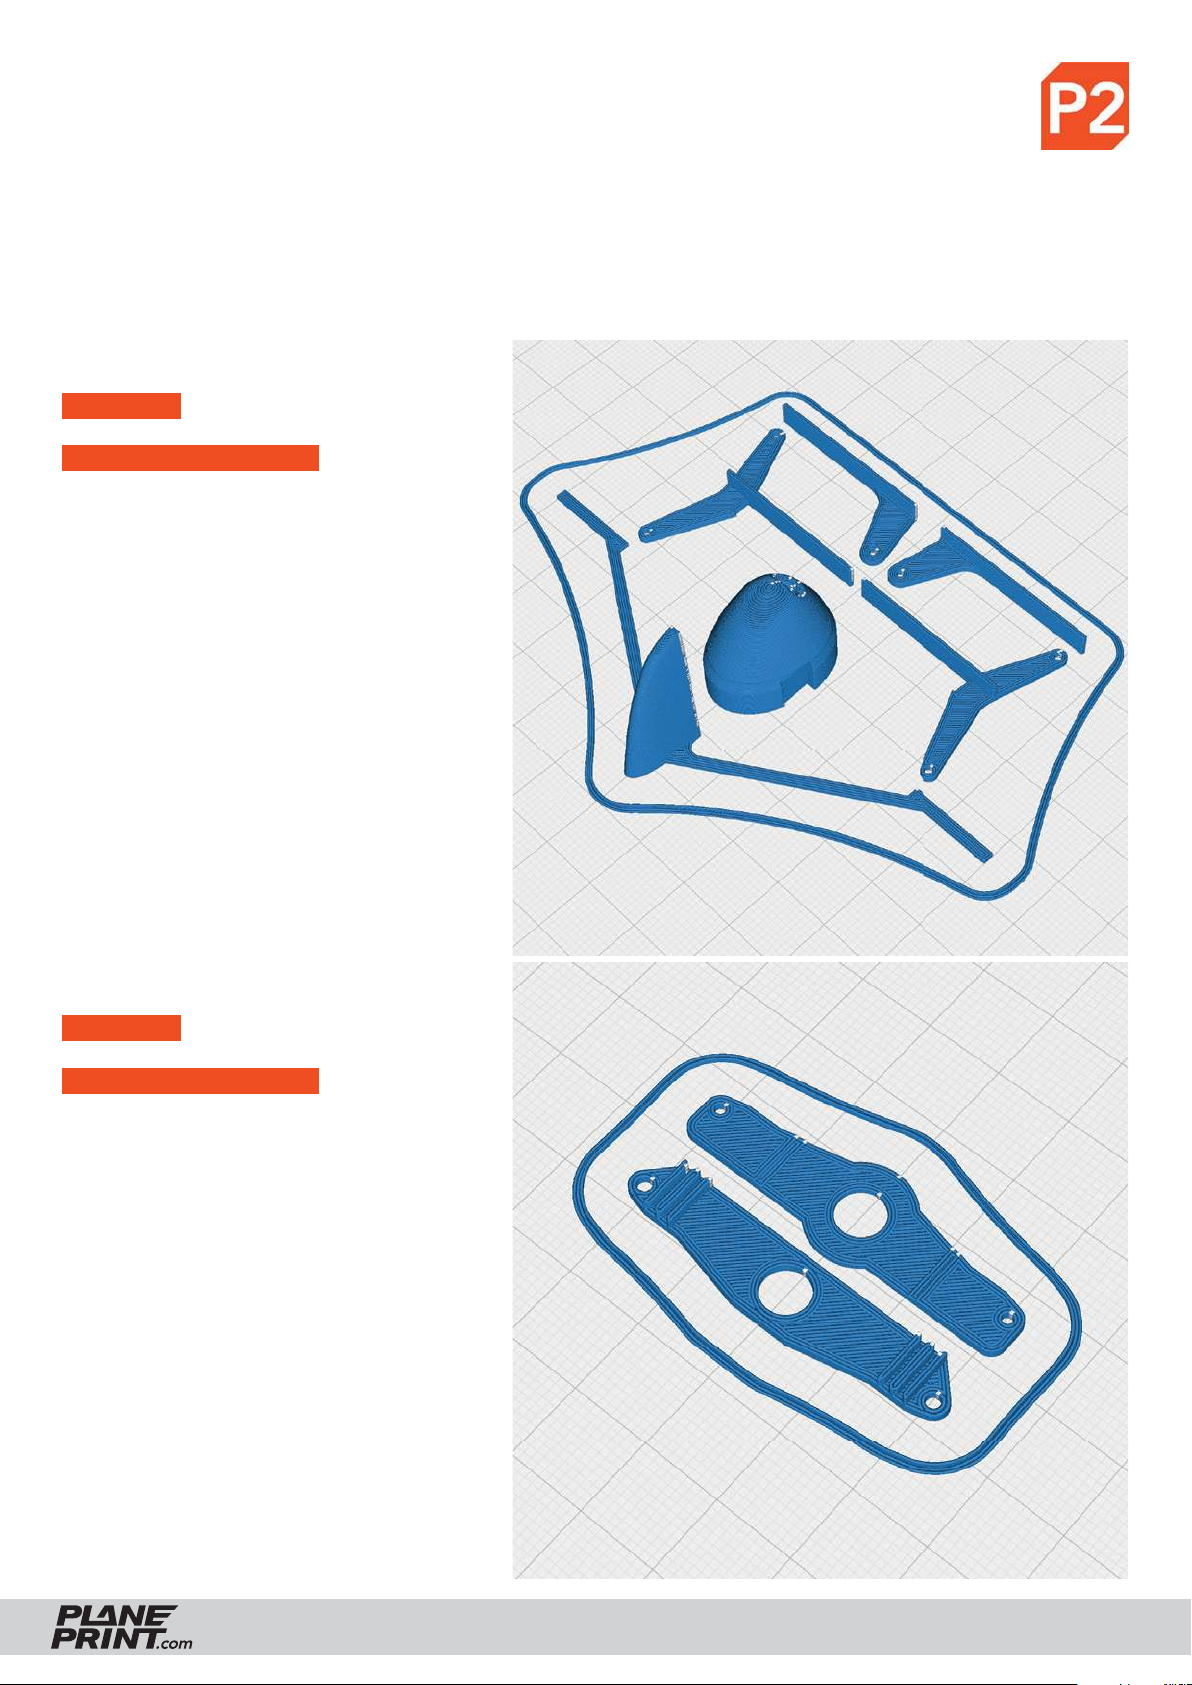
PROFILE P2_Hollowbody PLA or Tough PLA
The information about the basic settings you can fi nd on our website at PRINT.
Please note the additional settings for the individual parts!
P2_Parts 2–S1.stl
MATERIAL PLA, Weight: ~ 4 g
ADDITIONAL SETTINGS
None required
P2_Servo lever.stl
MATERIAL PLA, Weight: ~ 1 g
ADDITIONAL SETTINGS
None required
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
8
Page 9
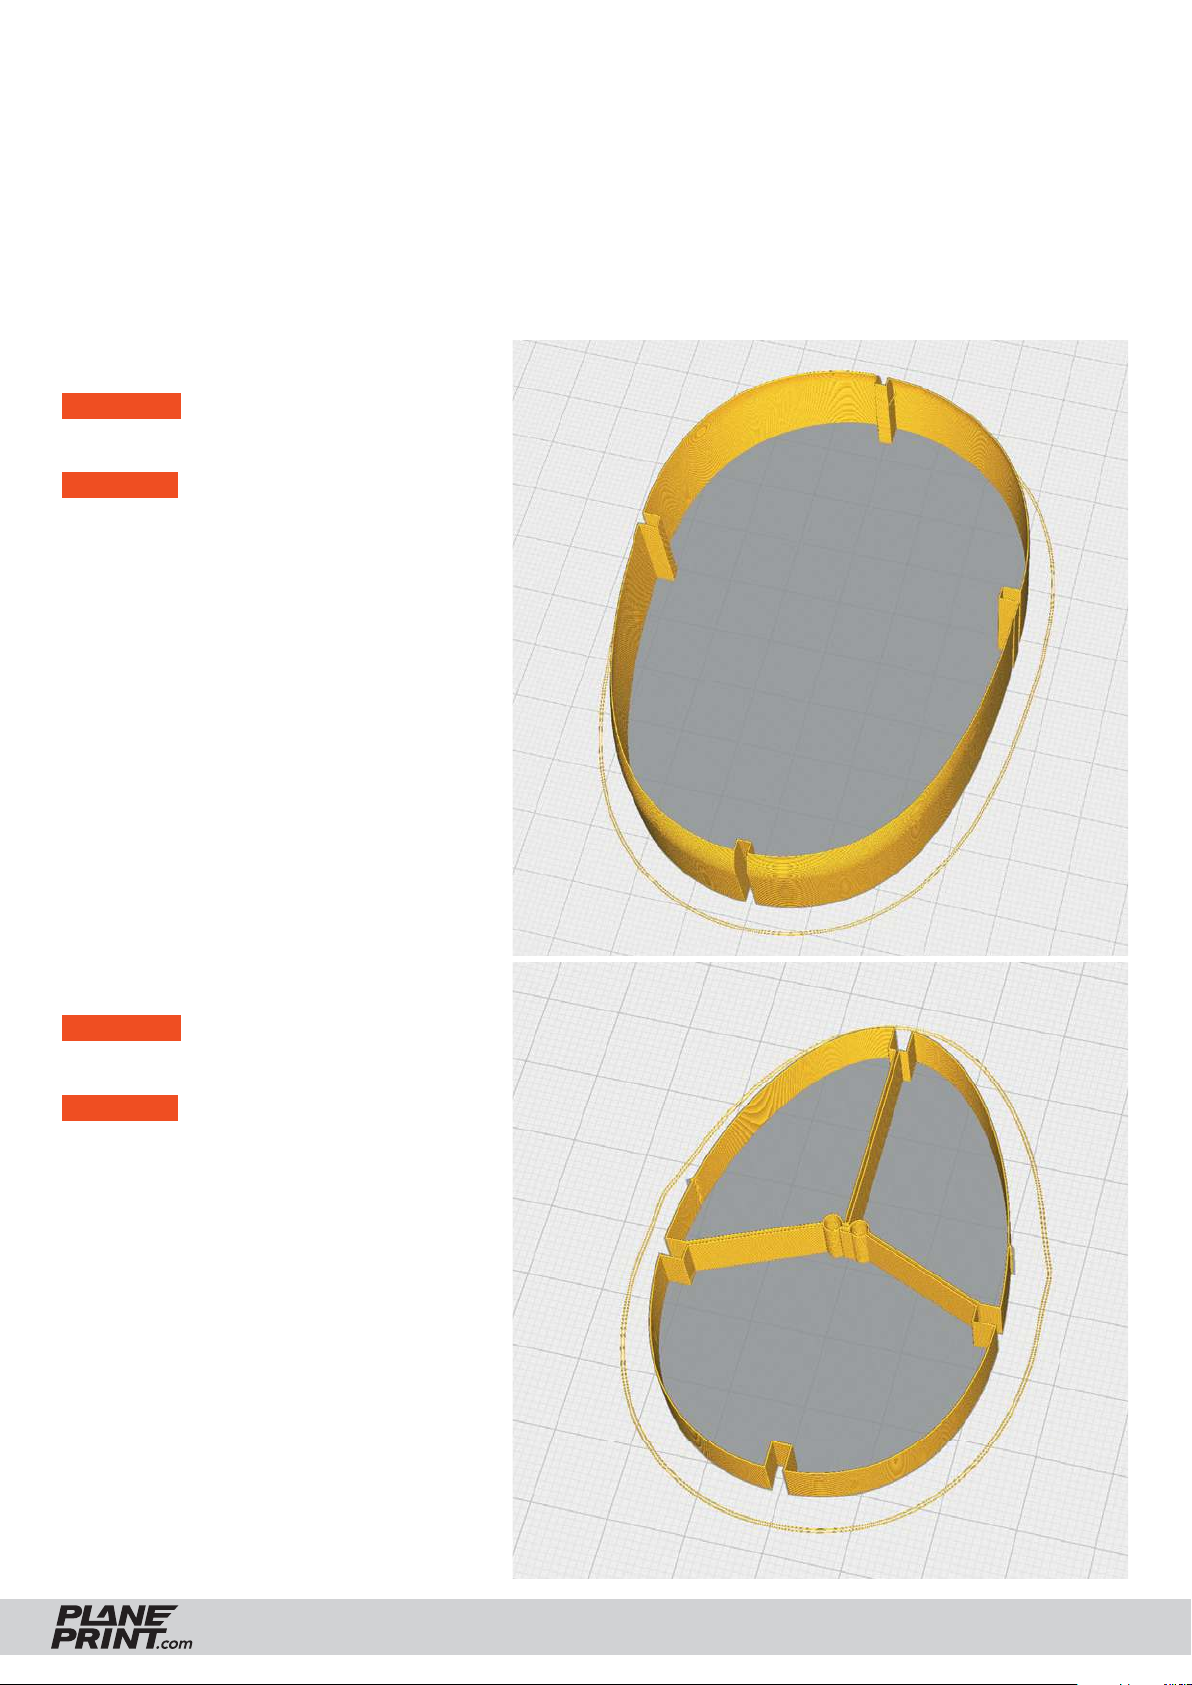
SPIRALIZE/VASE MODE
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
– Light-Weight LW-PLA!
V_C1-2–S1.stl
MATERIAL LW-PLA, ~ 1 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
V_C2-3–S1.stl
MATERIAL LW-PLA, ~ 1 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
9
Page 10
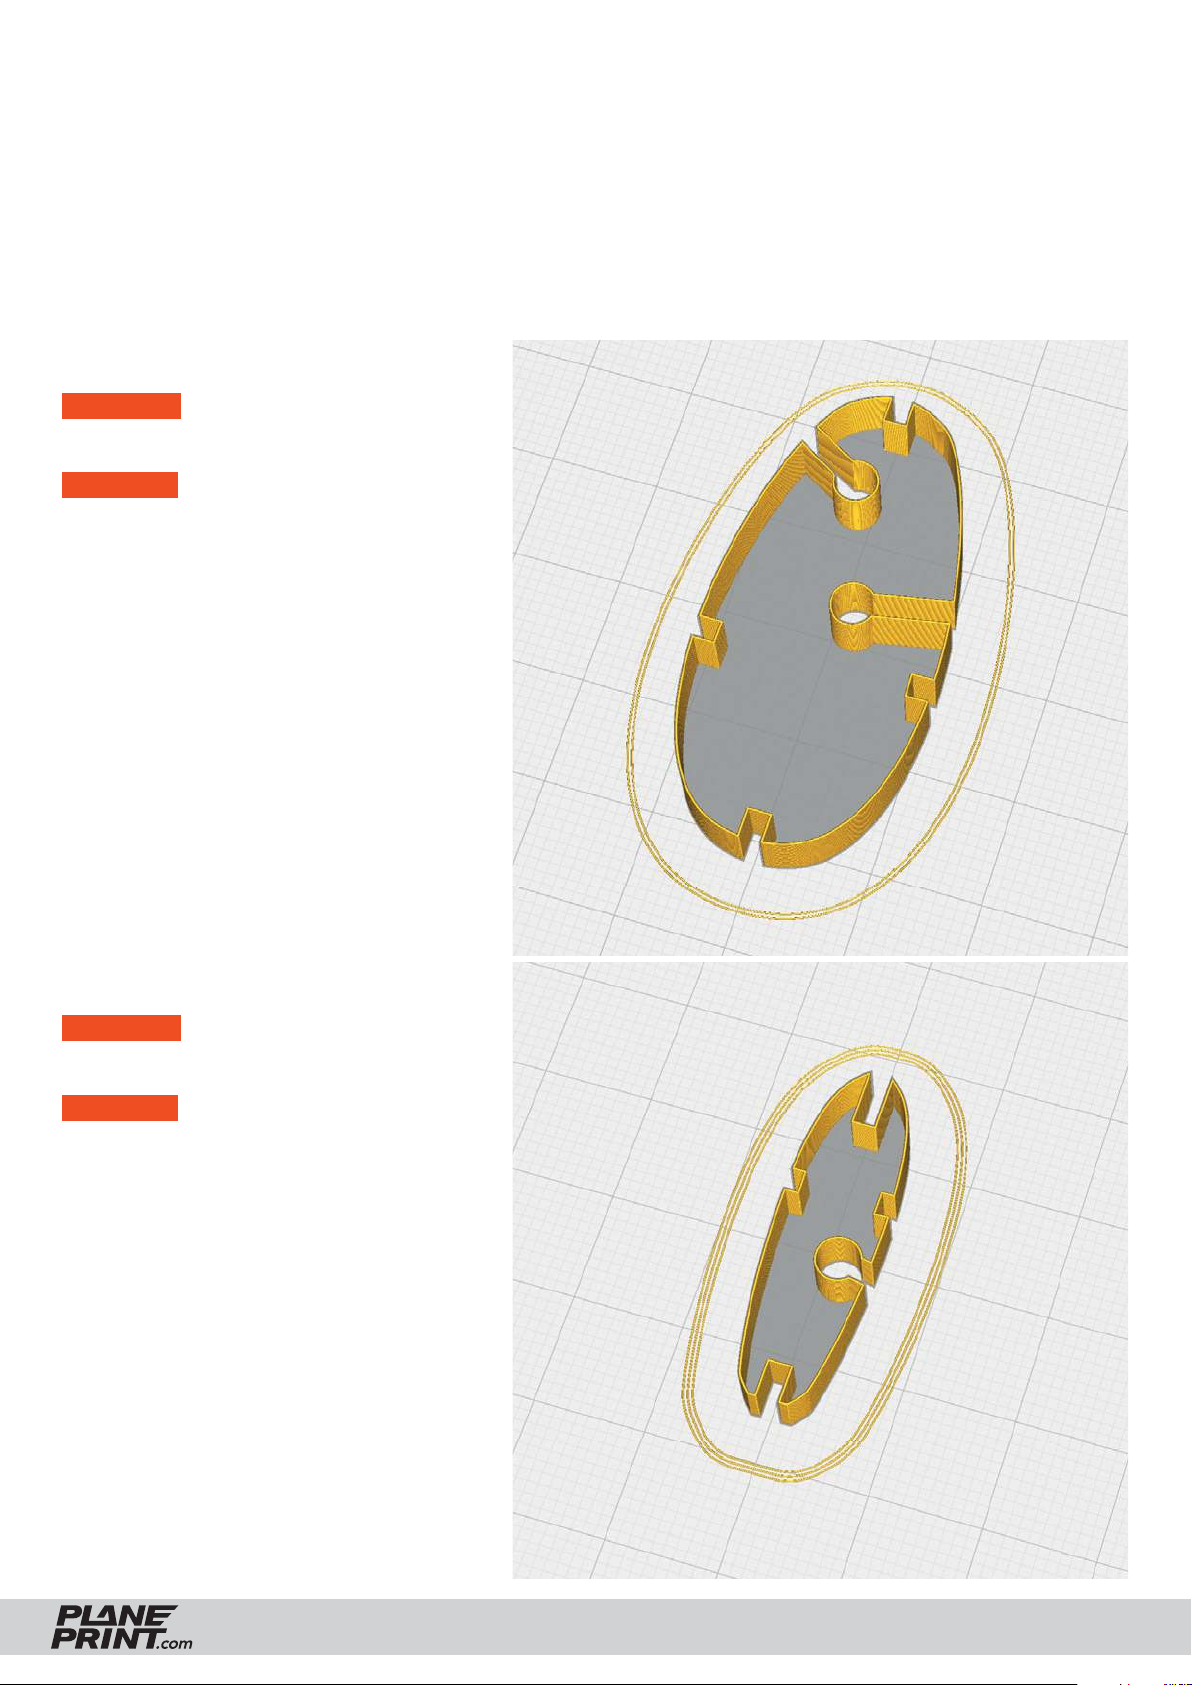
SPIRALIZE/VASE MODE
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
– Light-Weight LW-PLA!
V_C3-4–S1.stl
MATERIAL LW-PLA, ~ 1 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
V_C4-5–S1.stl
MATERIAL LW-PLA, ~ 1 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
10
Page 11
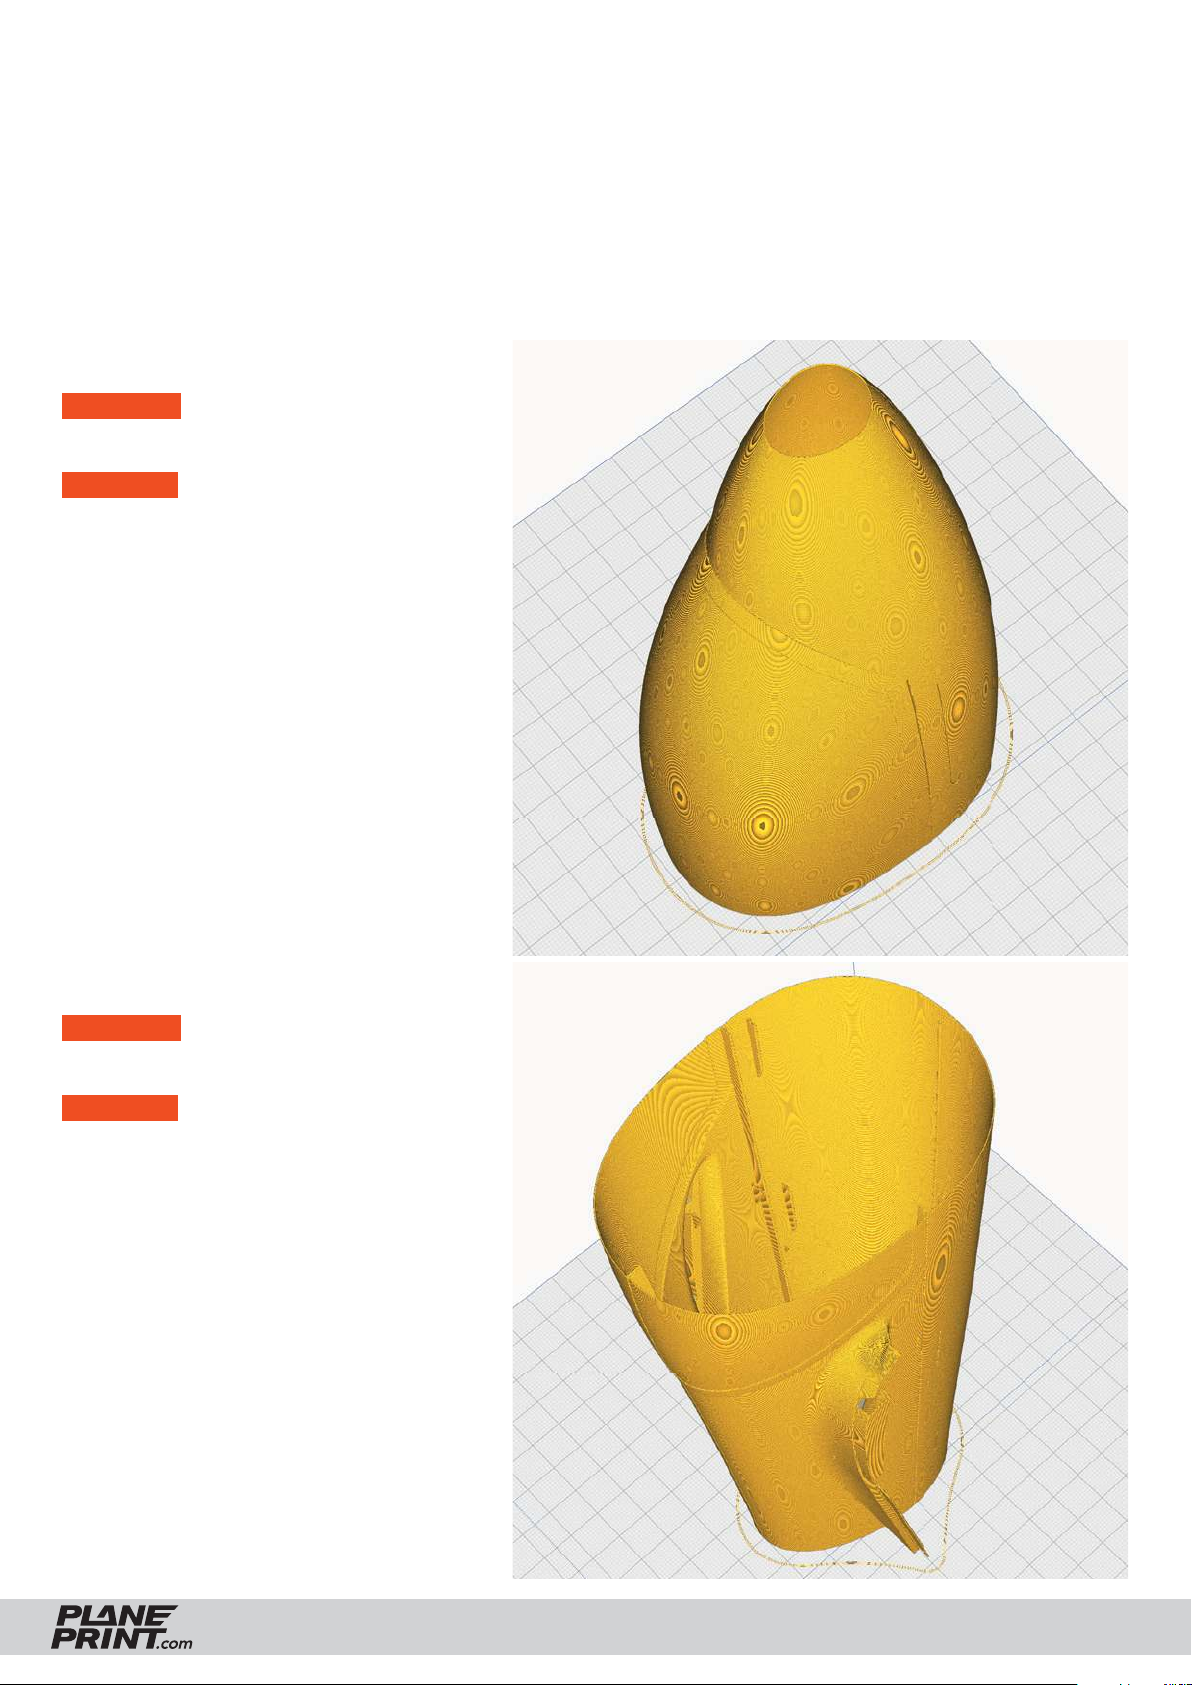
SPIRALIZE/VASE MODE – Light-Weight LW-PLA!
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
V_Fuselage 1–S1.stl
MATERIAL LW-PLA, ~ 10 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
V_Fuselage 2–S1.stl
MATERIAL LW-PLA, ~ 13 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
11
Page 12
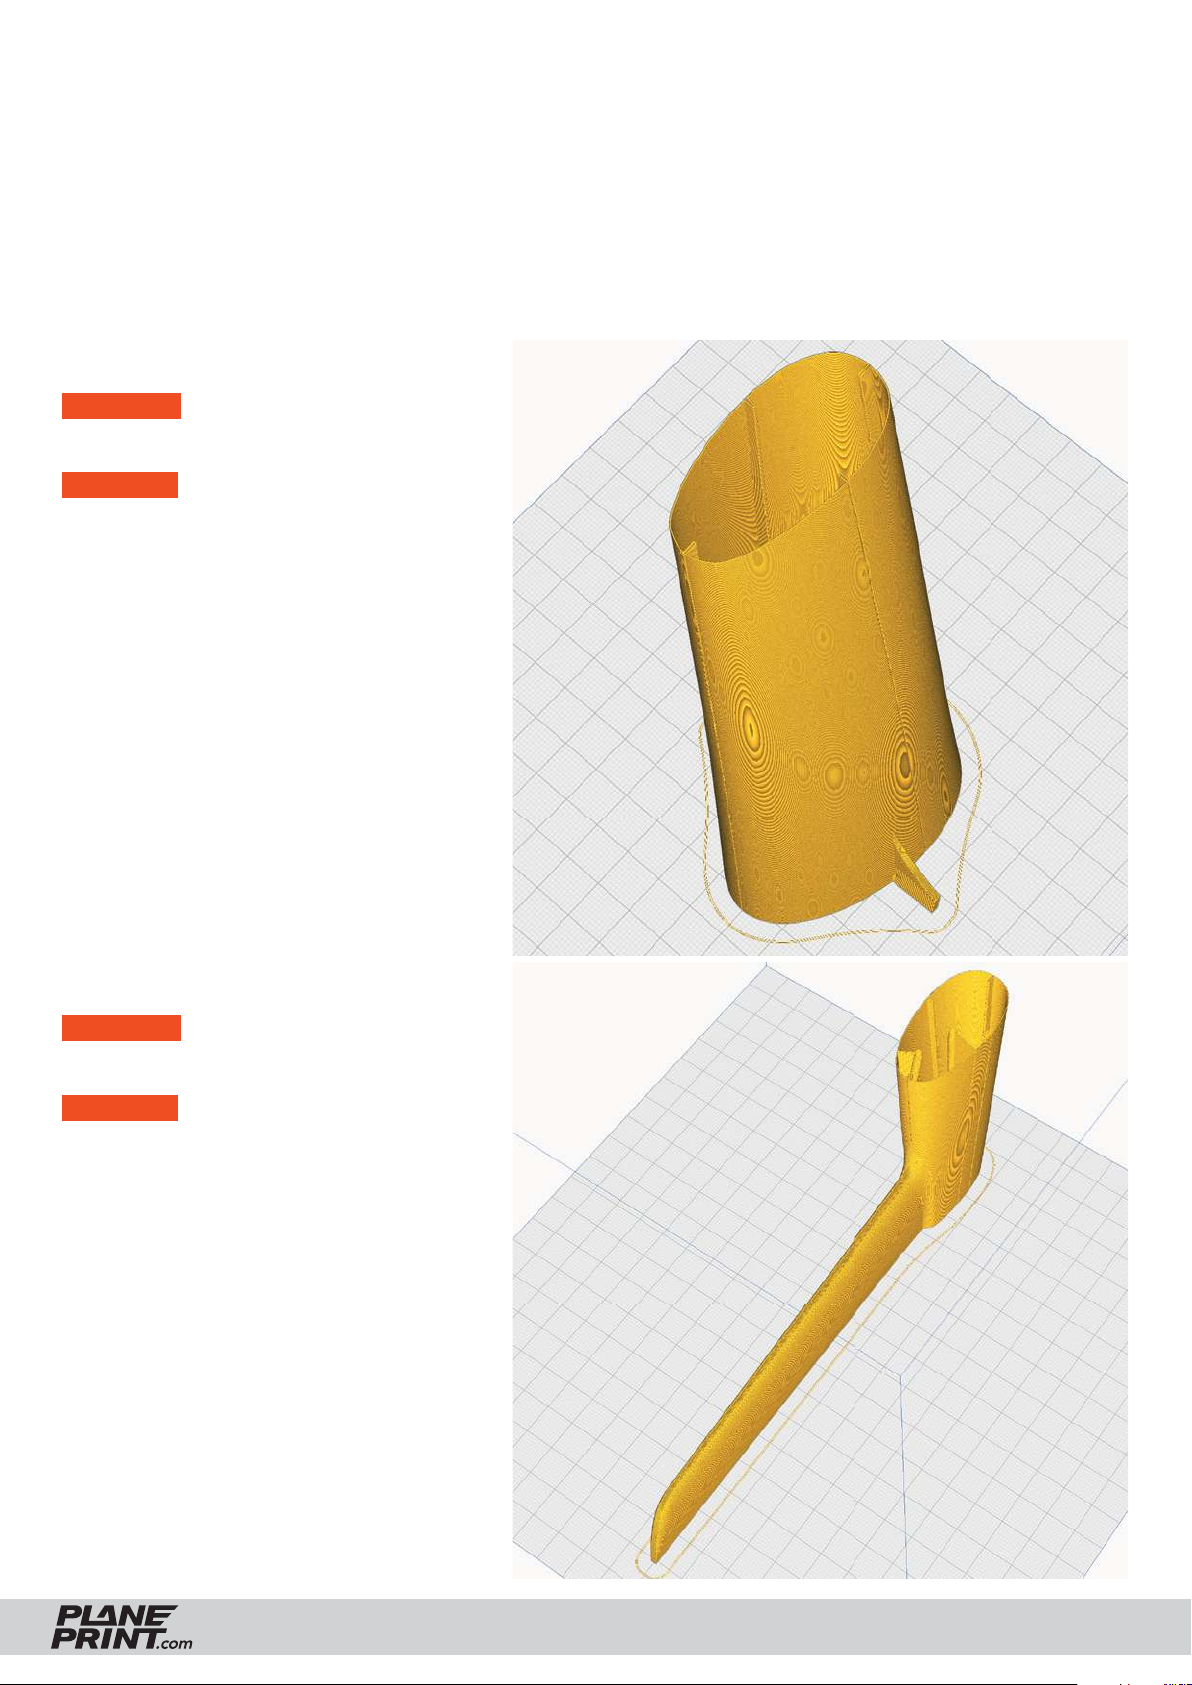
SPIRALIZE/VASE MODE – Light-Weight LW-PLA!
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
V_Fuselage 3–S1.stl
MATERIAL LW-PLA, ~ 8 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
V_Fuselage 4–S1.stl
MATERIAL LW-PLA, ~ 6 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
12
Page 13
SPIRALIZE/VASE MODE – Light-Weight LW-PLA!
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
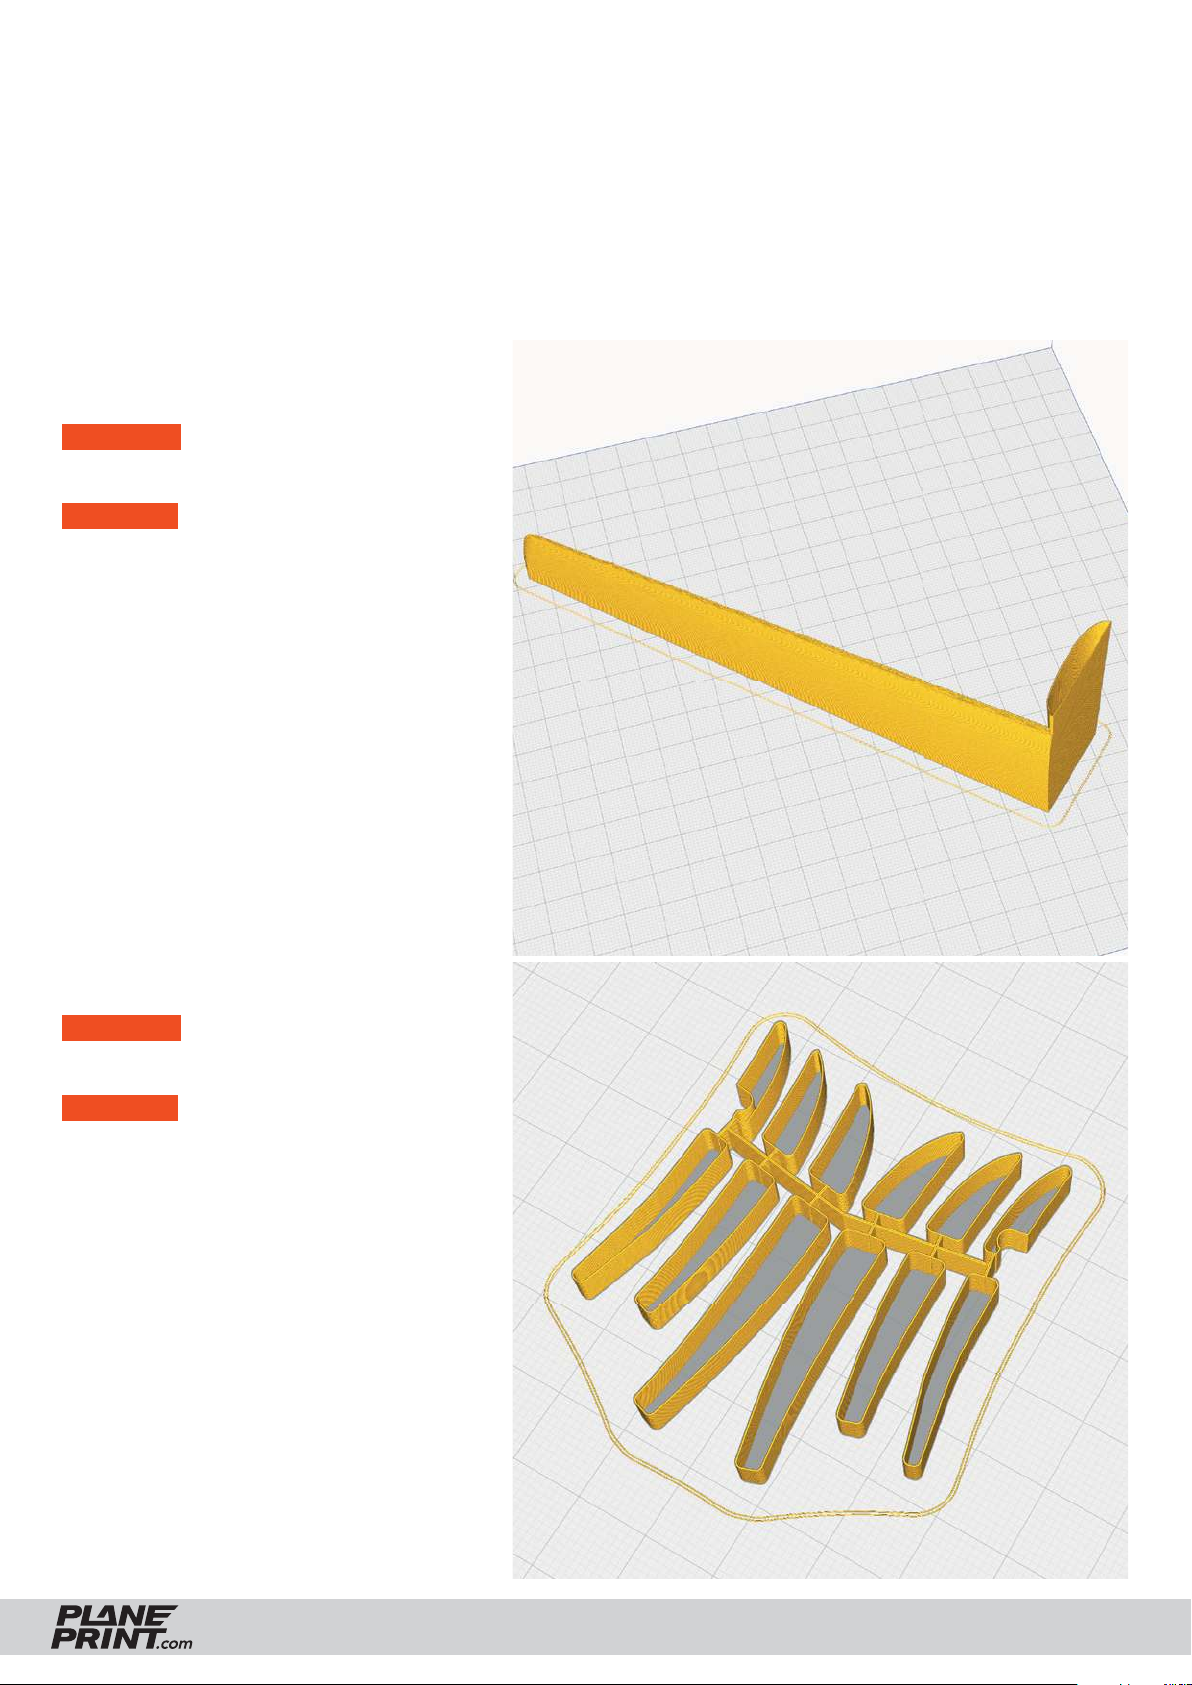
V_Fuselage 5 L–S1.stl and
V_Fuselage 5 R–S1.stl
MATERIAL LW-PLA, ~ 4 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
Wingconnect–S1.stl
MATERIAL LW-PLA, ~ 1 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
13
Page 14
SPIRALIZE/VASE MODE – Light-Weight LW-PLA!
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
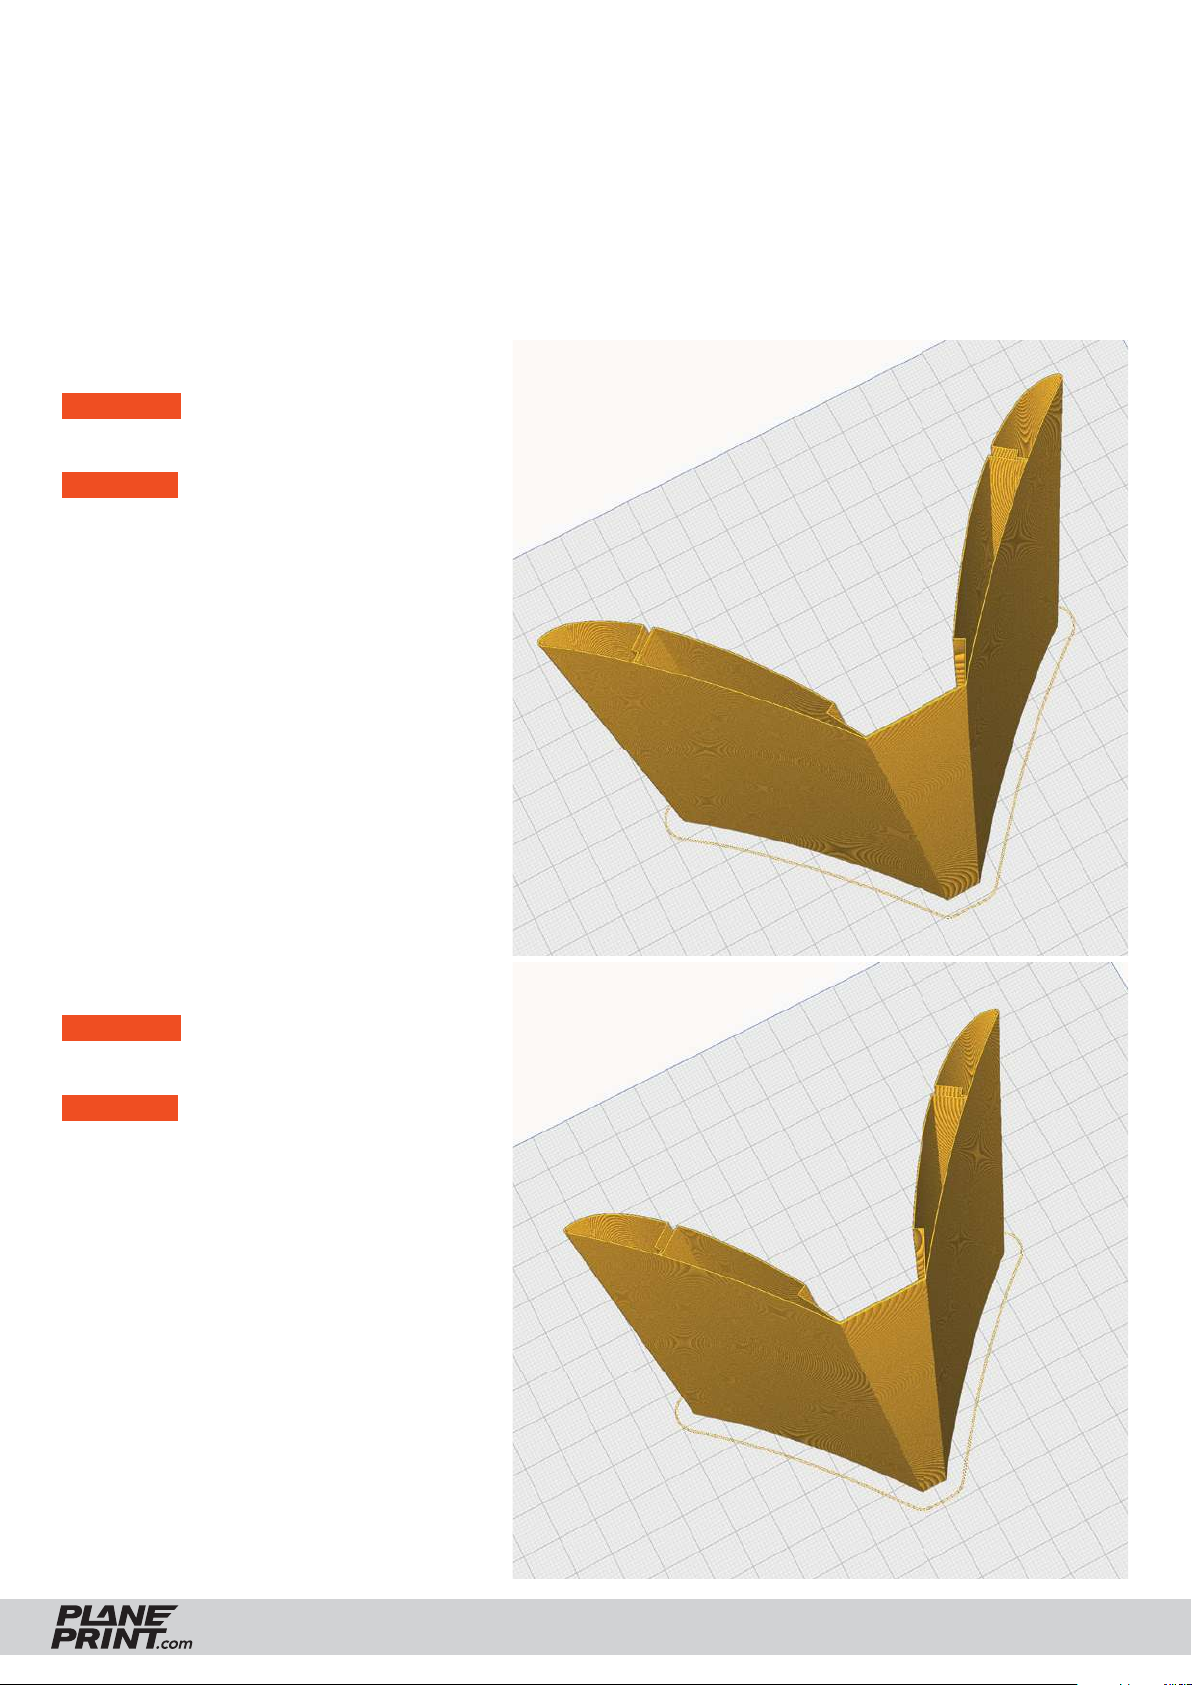
V_Wings 1–S1.stl
MATERIAL LW-PLA, ~ 15 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
V_Wings 2–S1.stl
MATERIAL LW-PLA, ~ 12 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
14
Page 15
SPIRALIZE/VASE MODE – Light-Weight LW-PLA!
The following parts must be sliced with the Funktion Spiralize Outer Contour (Cura) or Spiral Vase (Prusa Slicer).
For these parts, only the outer wall (1 line/perimeter) is printed without Z-seam, no top and bottom layers.
It is essential to print these parts with LW-PLA!
Basic settings for LW-PLA: Please follow the instructions in our WINGTEST AND CALIBRATION TOOL
on our website for correct adjustment!
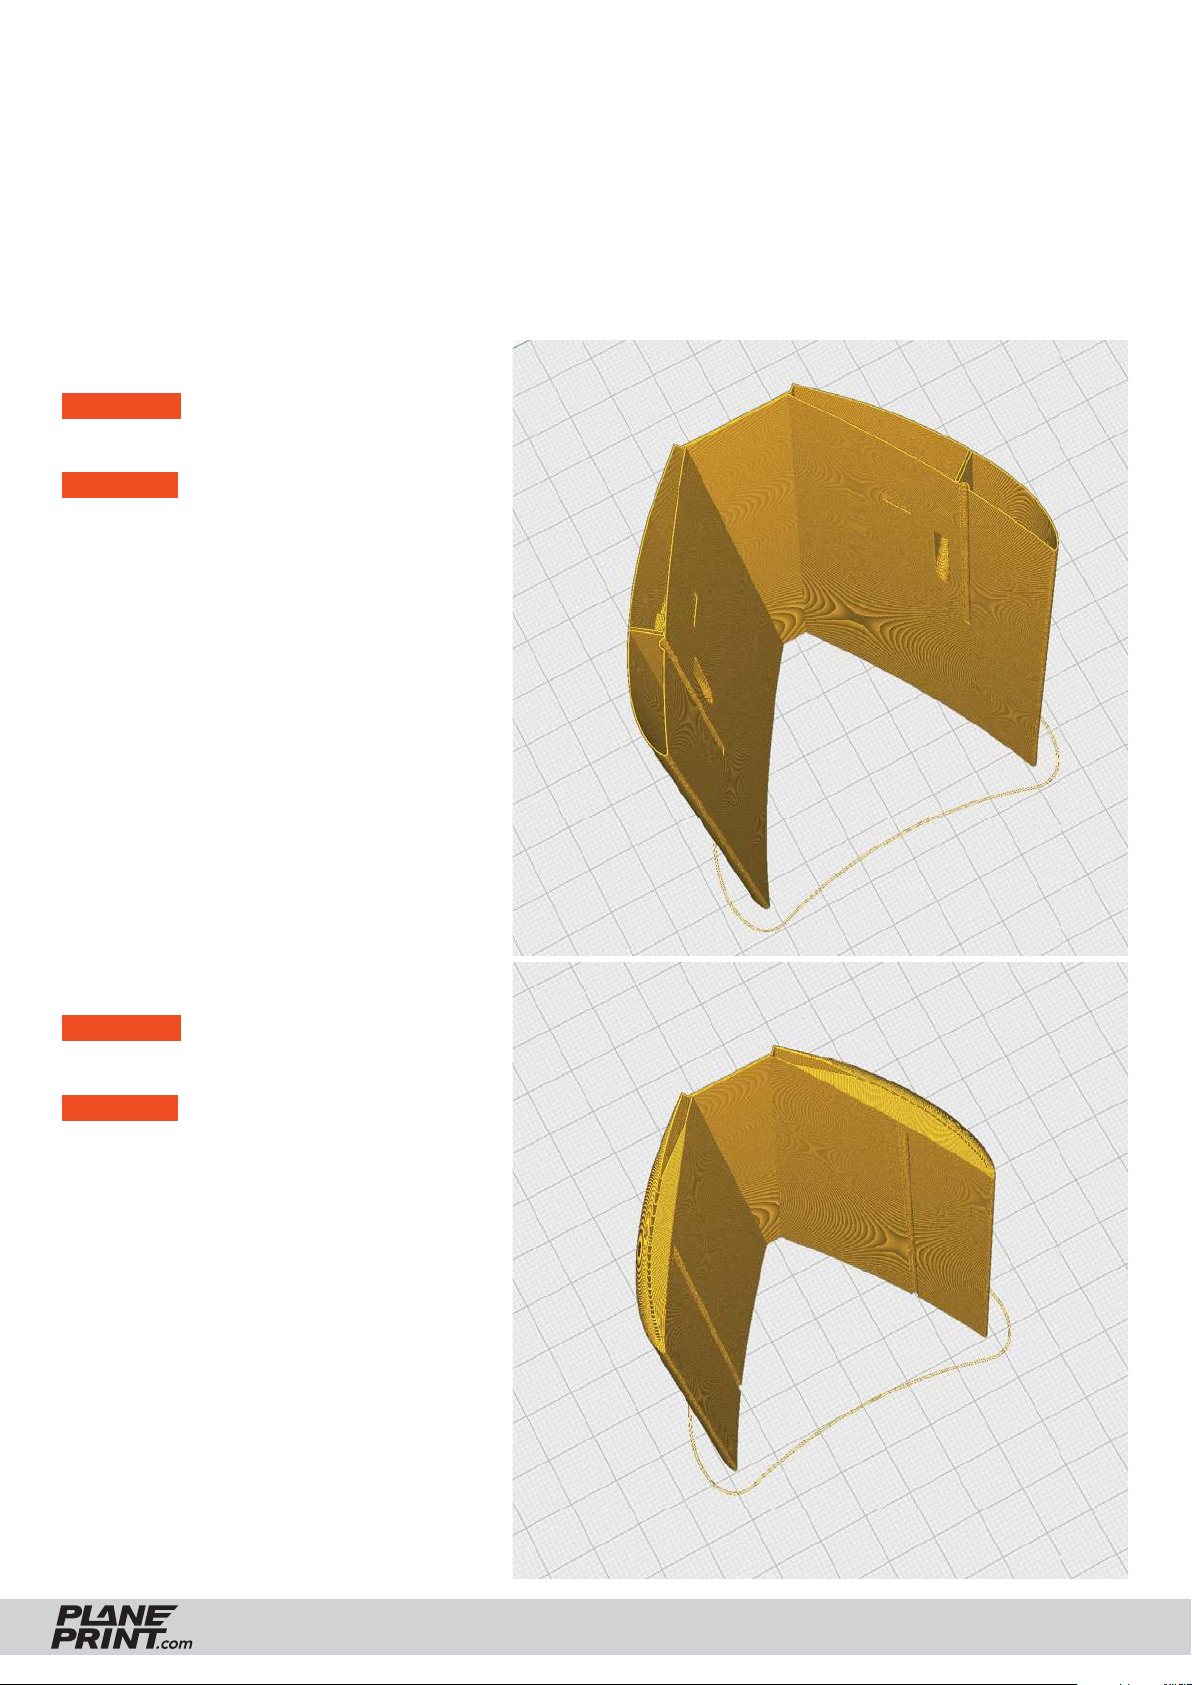
V_Wings 3–S1.stl
MATERIAL LW-PLA, ~ 11 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
V_Wings 4–S1.stl
MATERIAL LW-PLA, ~ 8 g*
*Weighed (approximate guideline)
SETTINGS
• Layer Height: 0.25 mm
• Wall Line Count/Perimeters: 1
• Spiralize Outer Contour (Cura)/
Spiral Vase (Prusa)
• Top and Bottom Layers: 0
• Flow, Temp and Speed suitable for LW PLA
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
15
Page 16
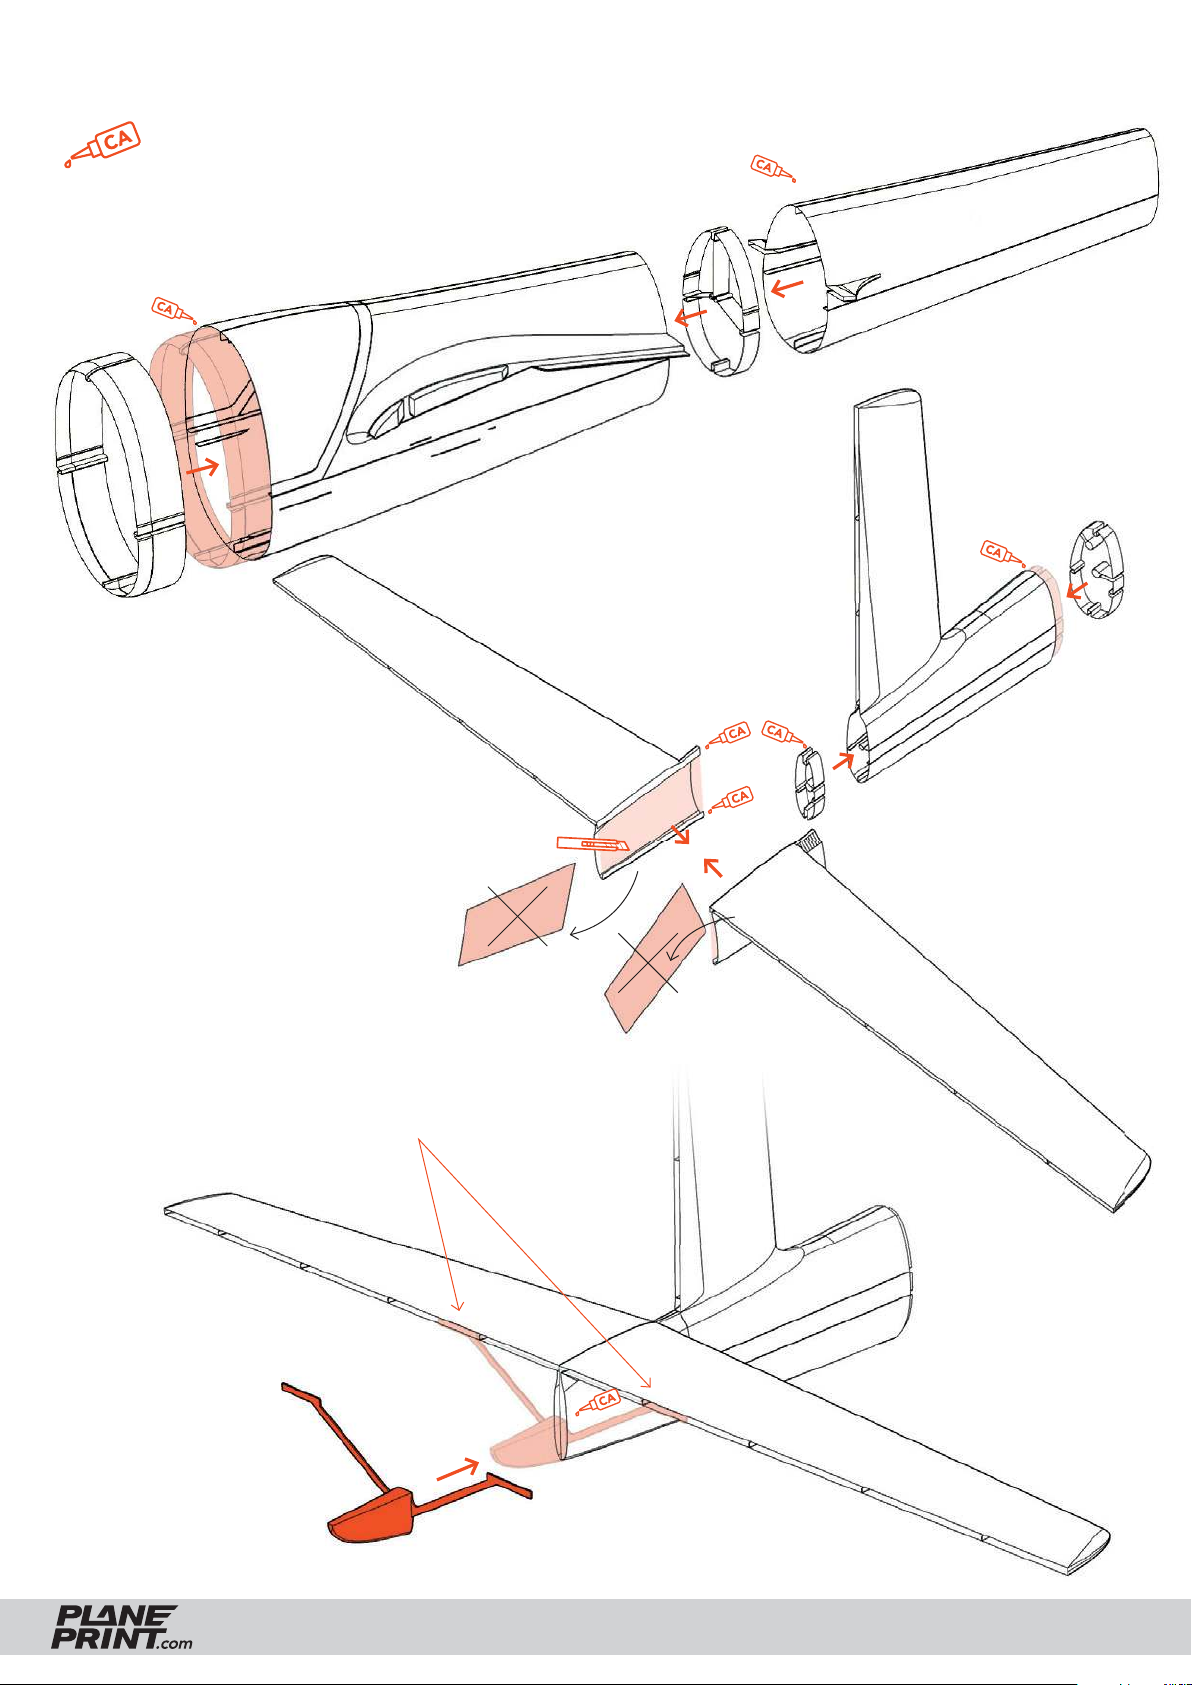
Fuselage assembly
medium liquid
First glue the positioning aids to one fuselage part, then
stick the second one on top. Make sure that the parts
are not twisted so that the tailplane is exactly aligned!
V_C1-2–S1.stl
After you have removed the support,
glue the two fuselage 5 parts together.
Then mount it to the fuselage using the
positioning aid V_C4-5–S1.stl.
V_Fuselage 2–S1.stl
V_Fuselage 5 L–S1.stl
V_C2-3–S1.stl
V_Fuselage 4–S1.stl
V_Fuselage 3–S1.stl
V_C3-4–S1.stl
V_C4-5–S1.stl
Remove support.
Please be careful with the knife!
Do NOT glue in these two places yet!
Here you can fi nally align the horizontal
stabilizer exactly parallel to the wing.
P2_Parts 2–S1.stl
V_Fuselage 5 R–S1.stl
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
16
Page 17
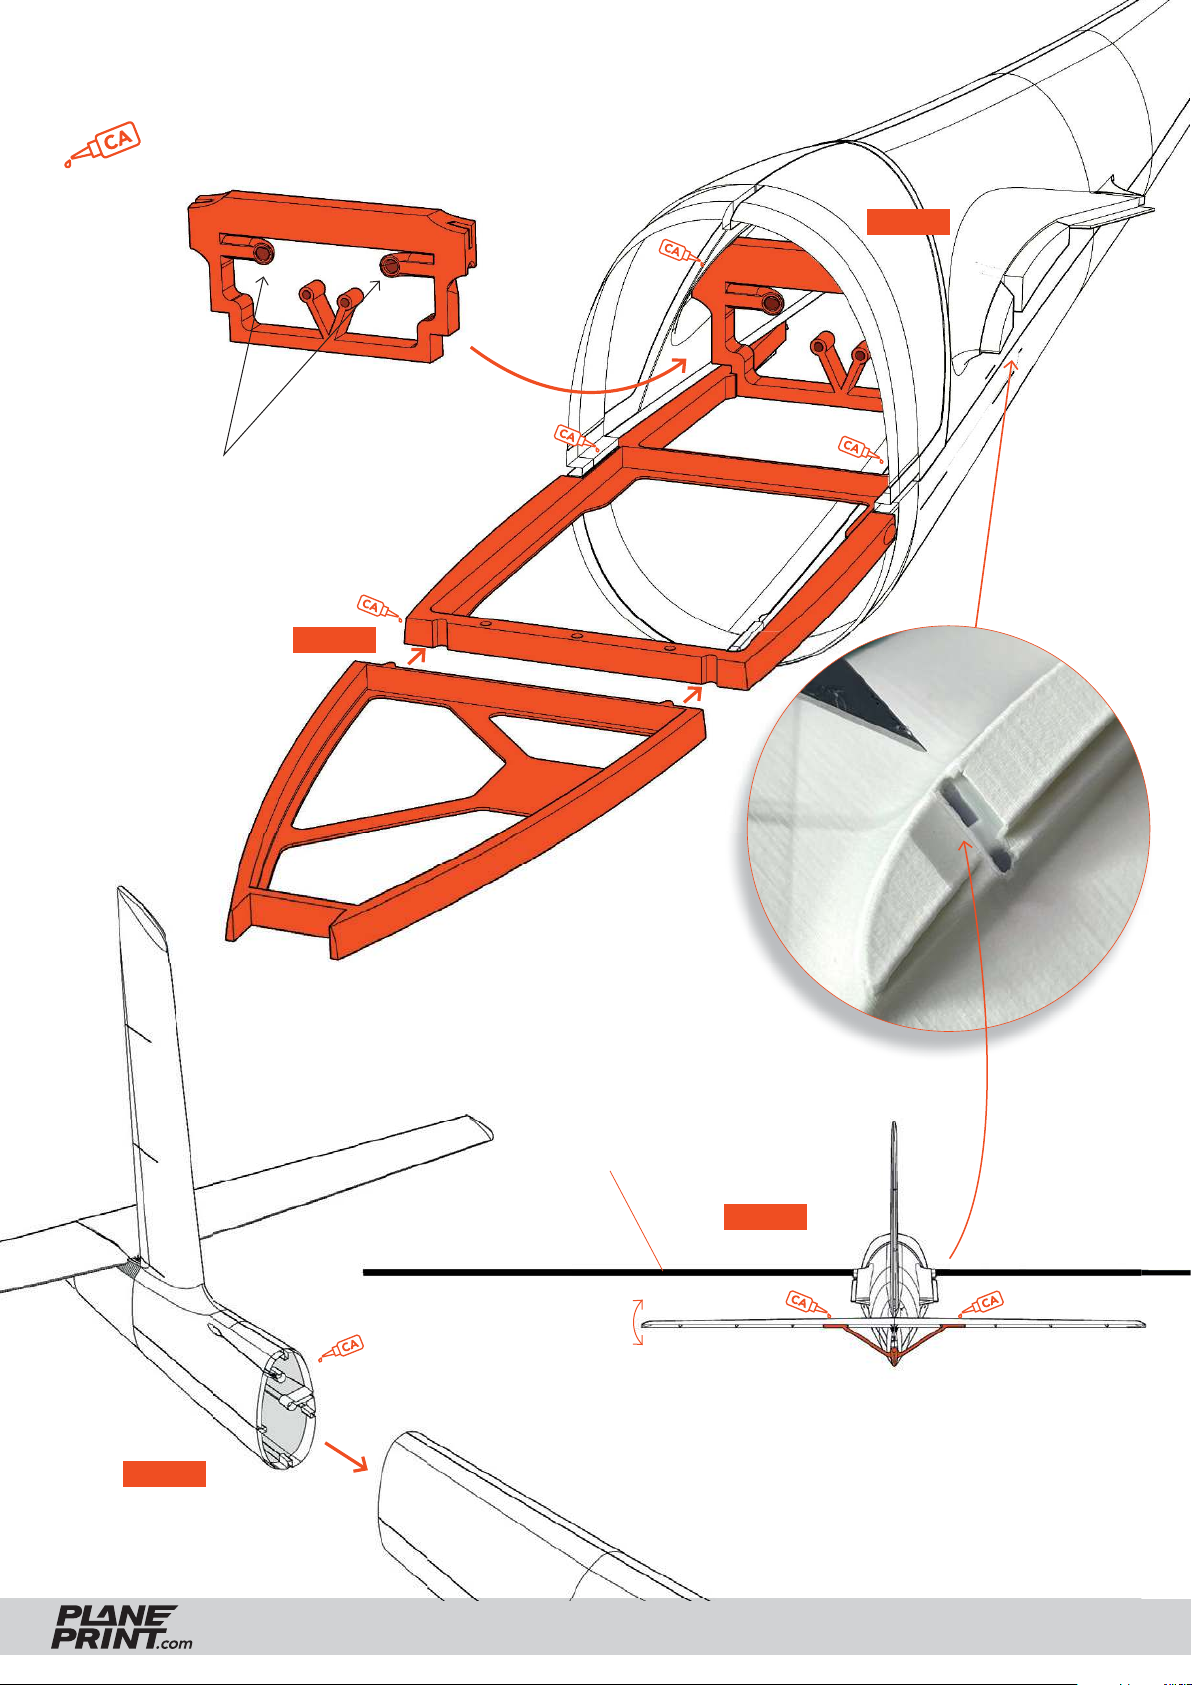
Fuselage assembly
medium liquid
P2_Parts 1–S1.stl
Insert these parts into the fuselage
exactly as shown in the picture. Make sure
that the openings are facing forward!
There are small bars in the fuselage that
serve as a positioning aid.
When all the parts are
correctly positioned,
allow thin CA glue
STEP 1
to run into the gaps
until everything is
well connected over a
large area.
P2_Frame–S1.stl
STEP 2
Carefully
open the holes
for carbon fi ber
strip and
linkage
with the
knife
STEP 3
SWIFT S1
Carbon fi ber strip 1*5*1000mm
STEP 4
Insert the carbon fi ber strip through
fuselage 2, align the horizontal
stabilizer parallel to it and glue the
two struts in place.
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
17
Page 18
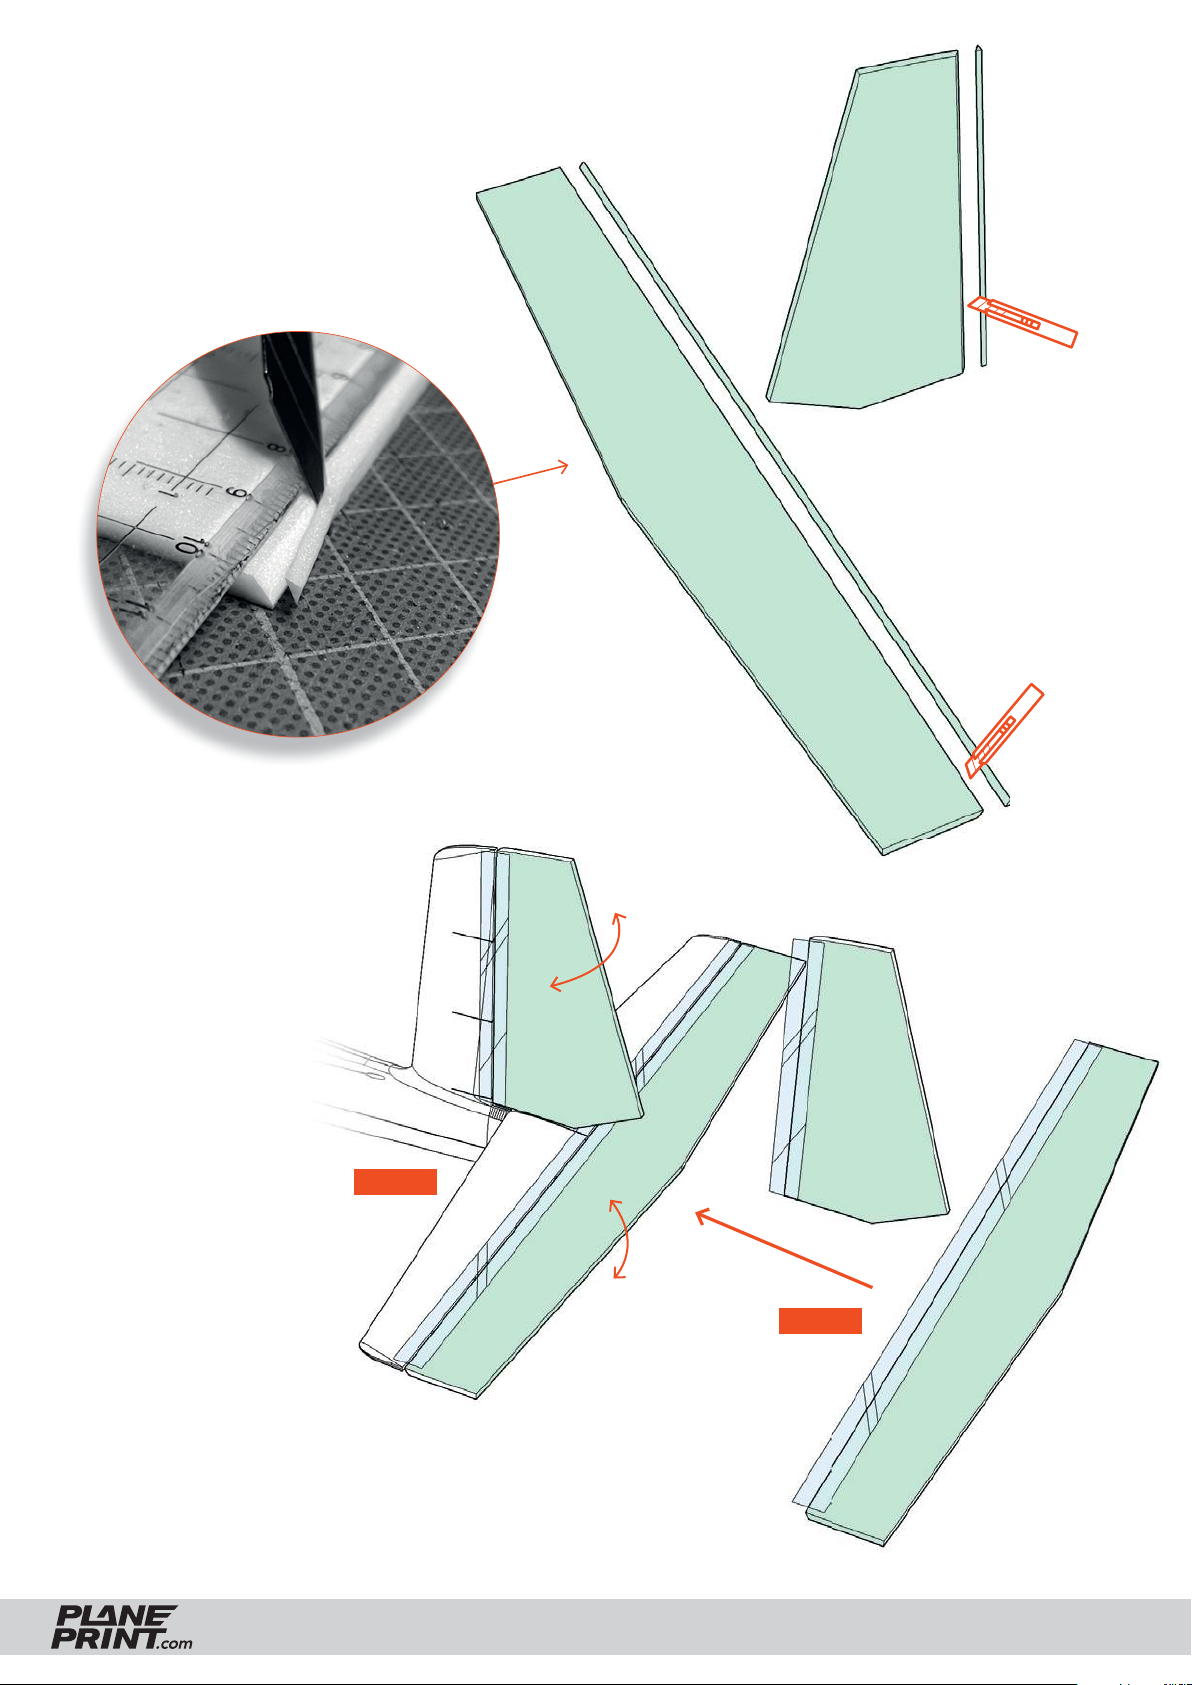
Elevator/Rudder assembly
Cut these two edges at an angle
of about 40°. You can also use
sandpaper for this.
Rudder
Elevator
The hinges are simply
made with thin adhesive
tape. To ensure that the
tape holds well, you
should coat the adhesive
area with UHU POR
beforehand. When the
glue is dry, fi rst stick the
tape to the elevator/
rudder, then attach it to
the fuselage.
Leave a small gap so that
the elevator/rudder can
be moved easily.
STEP 2
STEP 1
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
18
Page 19
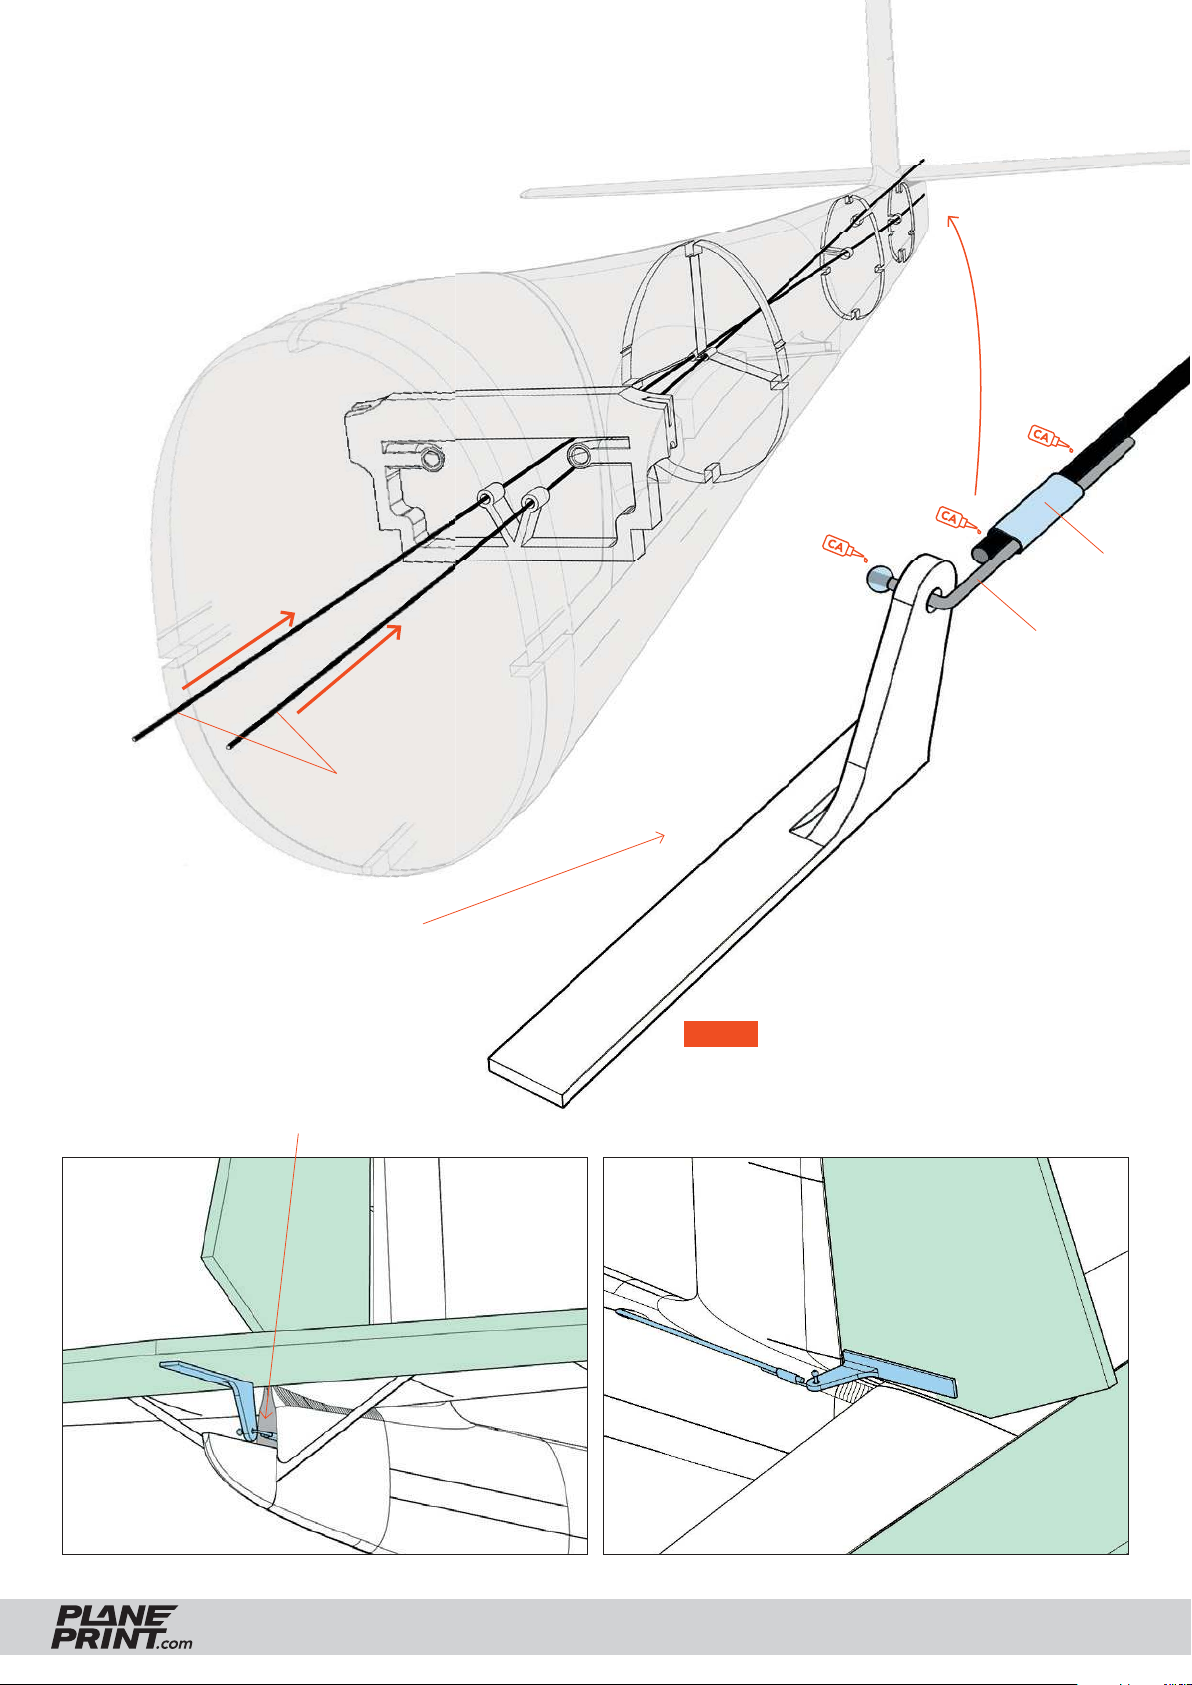
Elevator and rudder linkage
It is easier to insert the carbon rods
into the fuselage from the front.
Make sure that the rods are guided
through all eyelets!
Shrink tubing
or tape
Steel wire Ø0.6 mm
Carbon rods Ø1*60 mm
Prepare two linkages as shown here
Glue the control horns to the elevator and
rudder. When positioning the control horn
on the elevator, make sure that it cannot
get caught on the fuselage when the
elevator is moved downwards!
P2_Parts 2–S1.stl
NOTE With Depron you must use UHU POR
(or another glue suitable for Depron). Coat
both sides and allow the glue to dry. Then
position the control horn on the foam part.
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
19
Page 20
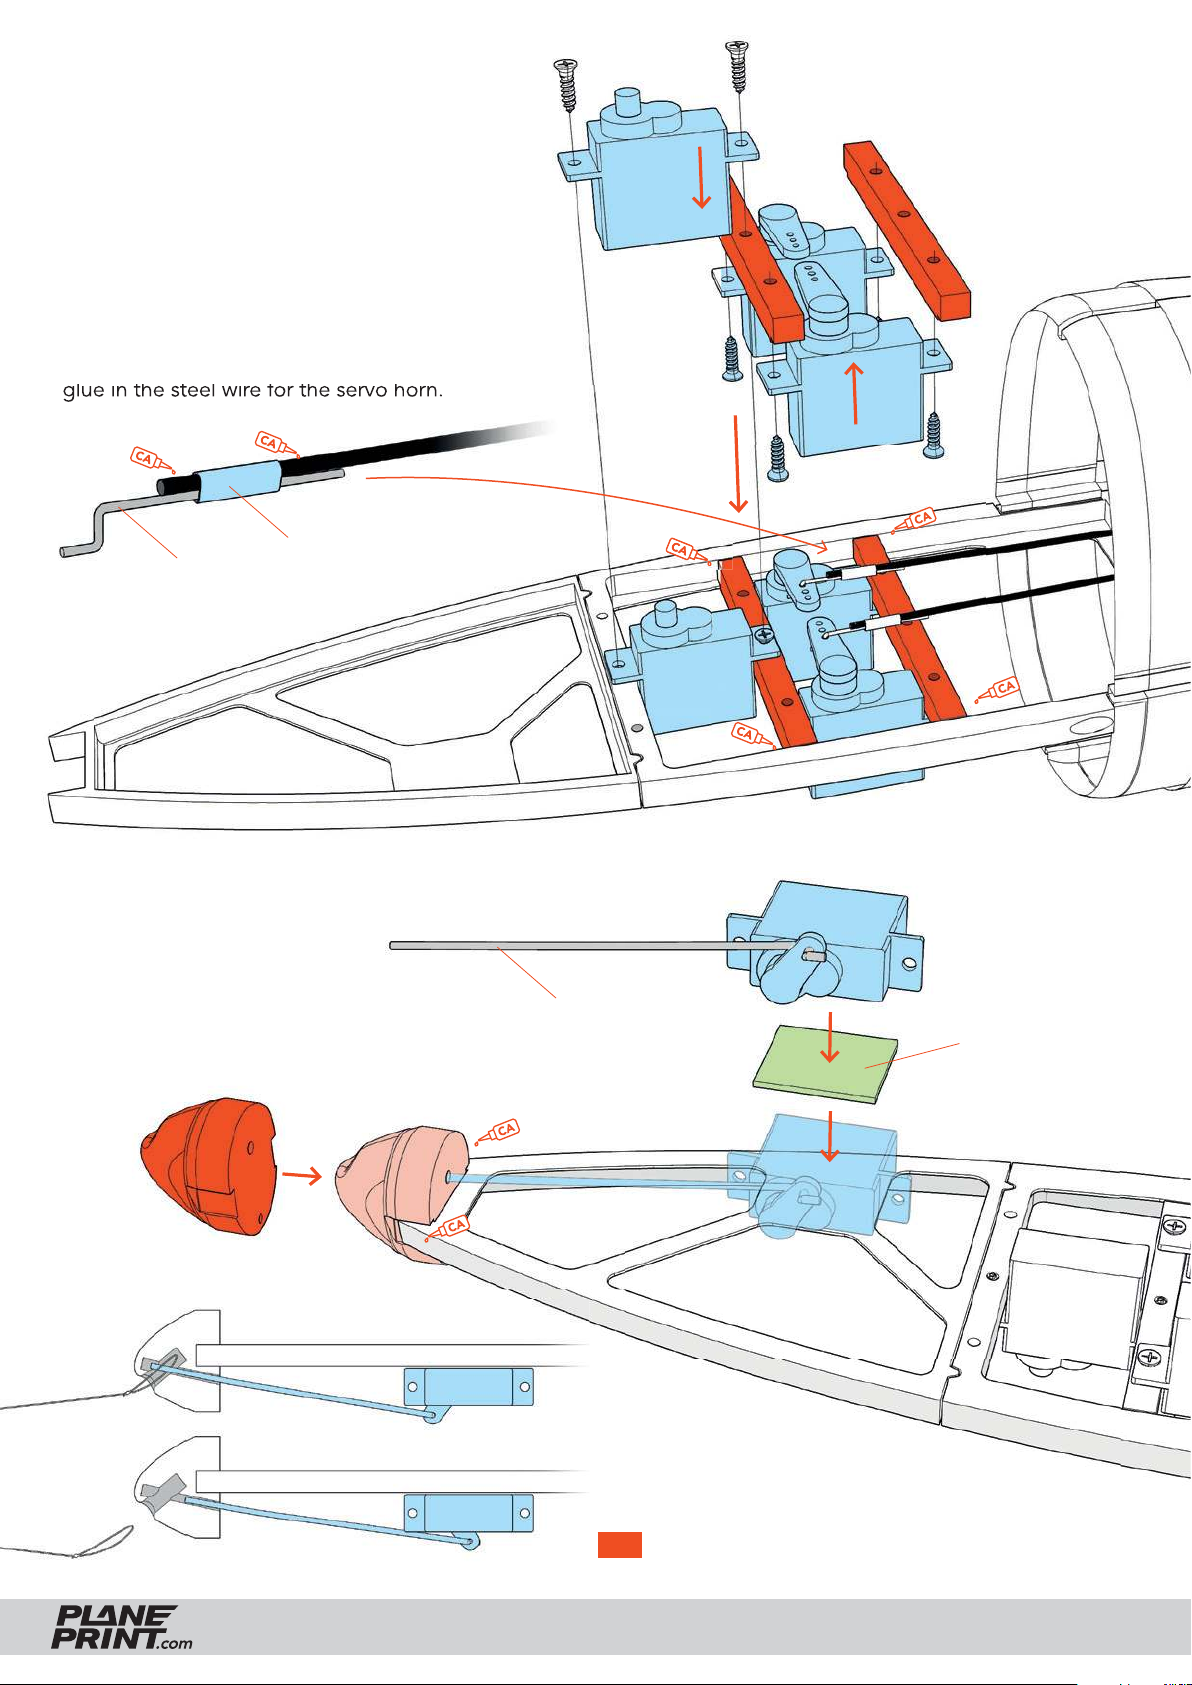
Servo mount
Mount the servos for the aileron, elevator
and rudder as shown here.
Do not forget to zero the servos fi rst.
Set the servos, elevator and rudder to
neutral, shorten the carbon rods and then
glue in the steel wire for the servo horn.
Shrink tubing or tape
Steel wire Ø0.6 mm
P2_Parts 1–S1.stl
Tow coupling
View from the bottom side!
P2_Parts 2–S1.stl
Steel wire Ø0.6 mm
Double-sided tape
or CA glue
Adjust the servo travel so that the
wire does not block at the front!
SWIFT S1
TIP The tow rope should be about 5 meters long.
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
20
Page 21
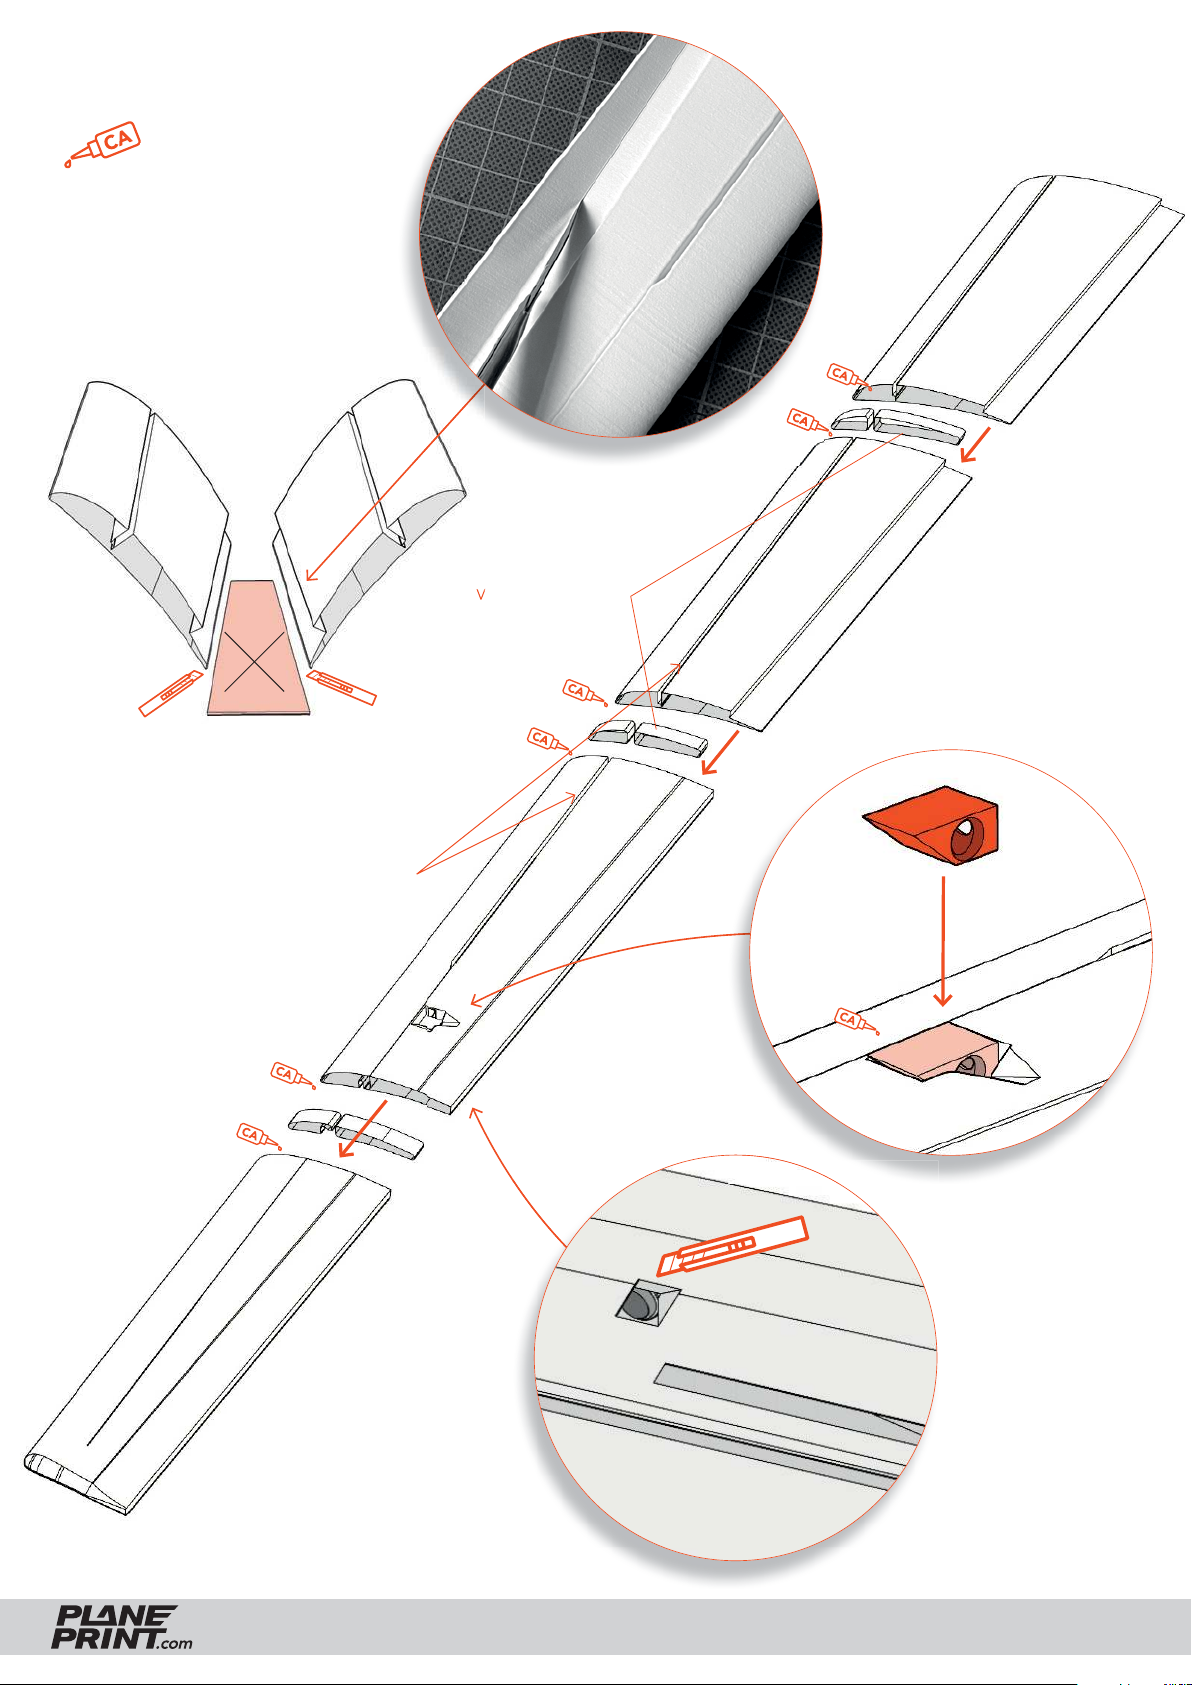
Wing assembly
medium liquid
First remove the support
of all wing parts.
Please be careful with the knife!
V_Wings 1–S1.stl
Place the wing parts on a fl at plate
and glue them together using the
wing connectors.
Be careful not to get any glue into
the gap at the top of the wing!
V_Wings 3–S1.stl
V_Wingconnect–S1.stl
V_Wings 2–S1.stl
P2_Parts 1–S1.stl
V_Wings 4–S1.stl
SWIFT S1
Carefully open the hole on the
underside of the wing with
a knife or drill.
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
21
Page 22
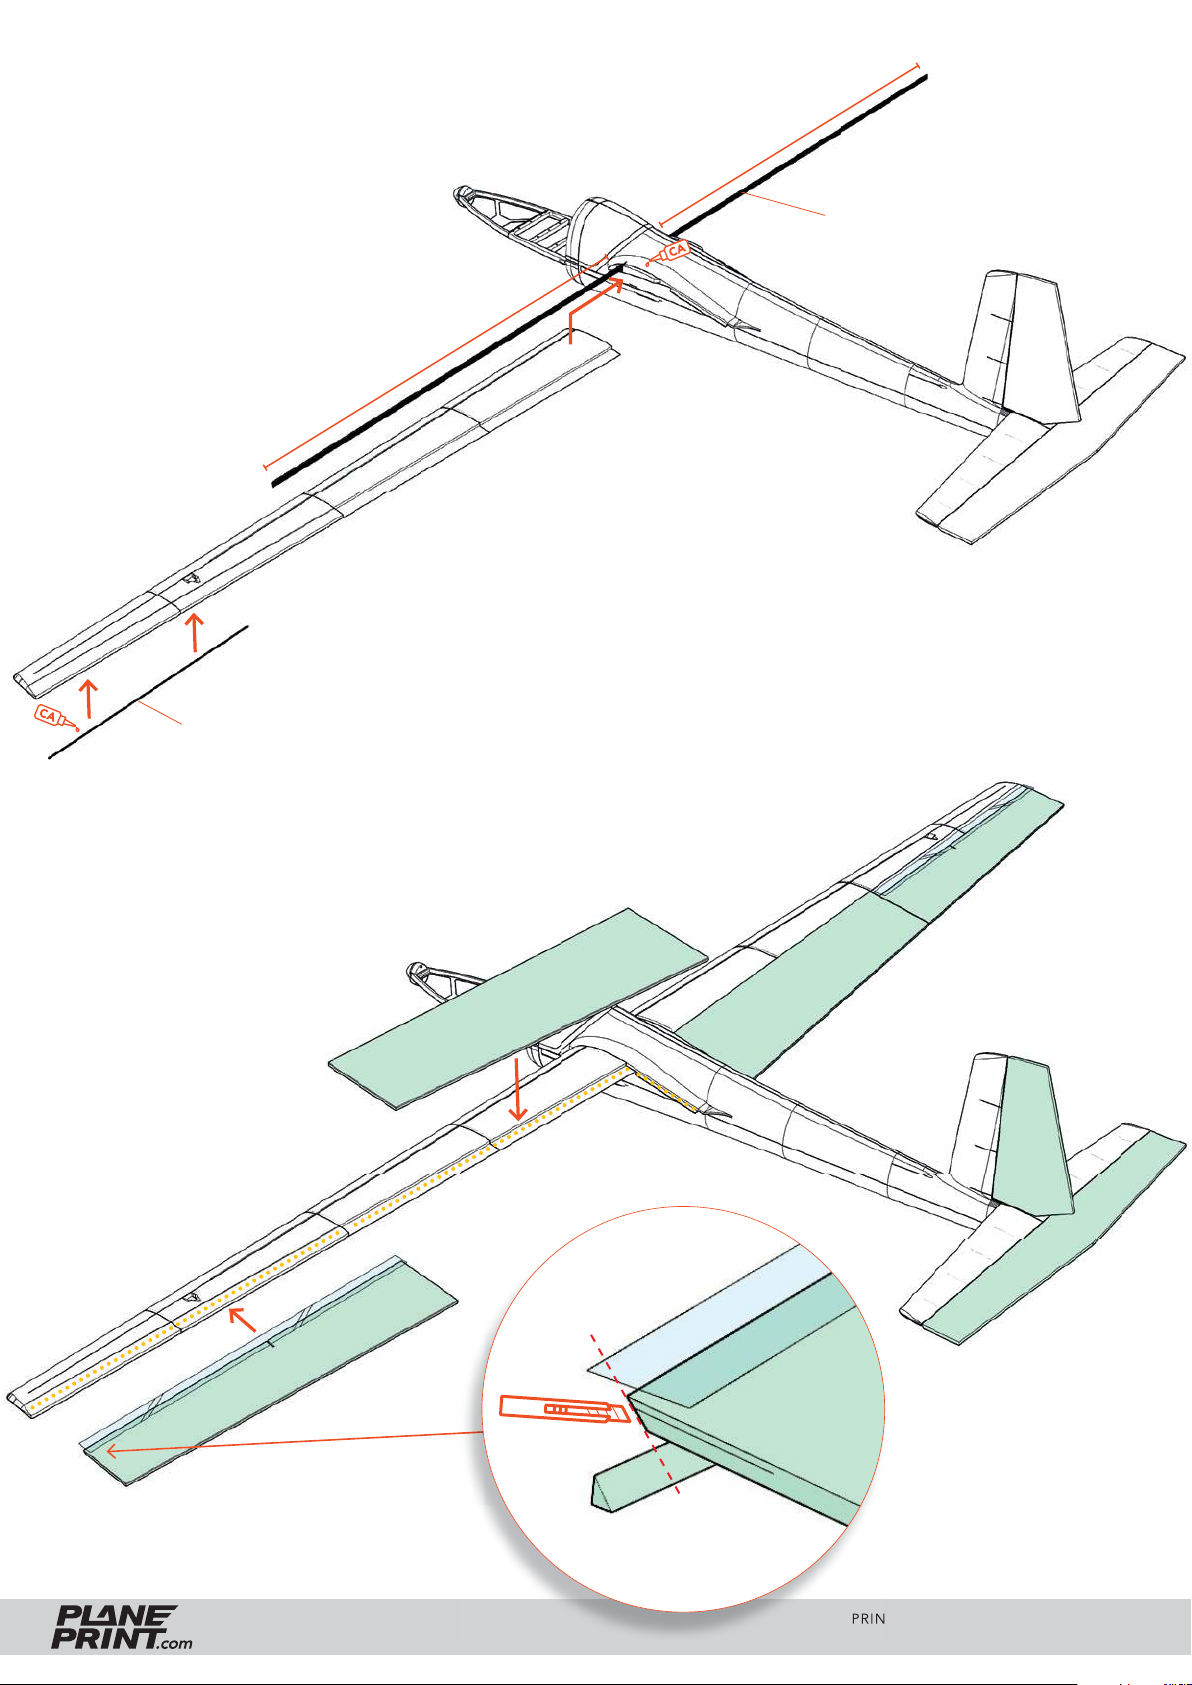
Wing assembly
Insert the carbon fi ber strip into the
fuselage and align it exactly in the
middle. Then let some thin CA glue
run into the gap so that it is fi xed to
the fuselage.
Carbon fi ber strip 1*5*1000mm
Glue the carbon rod into the
gap in the wing from below.
Carbon rod Ø1*215 mm
Glue the wing foam parts to the wing and
fuselage as shown in the picture. For Depron
use UHU POR (again, coat both sides, allow to
dry! and only then glue together).
Wing part
Then attach the wing
to the carbon strip and apply some
medium CA glue to the tab on the
fuselage. Push the wing all the way onto
the fuselage. Now let thin CA glue fl ow
into the gap along the entire carbon strip.
(still without glue)
Aileron
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
22
Page 23
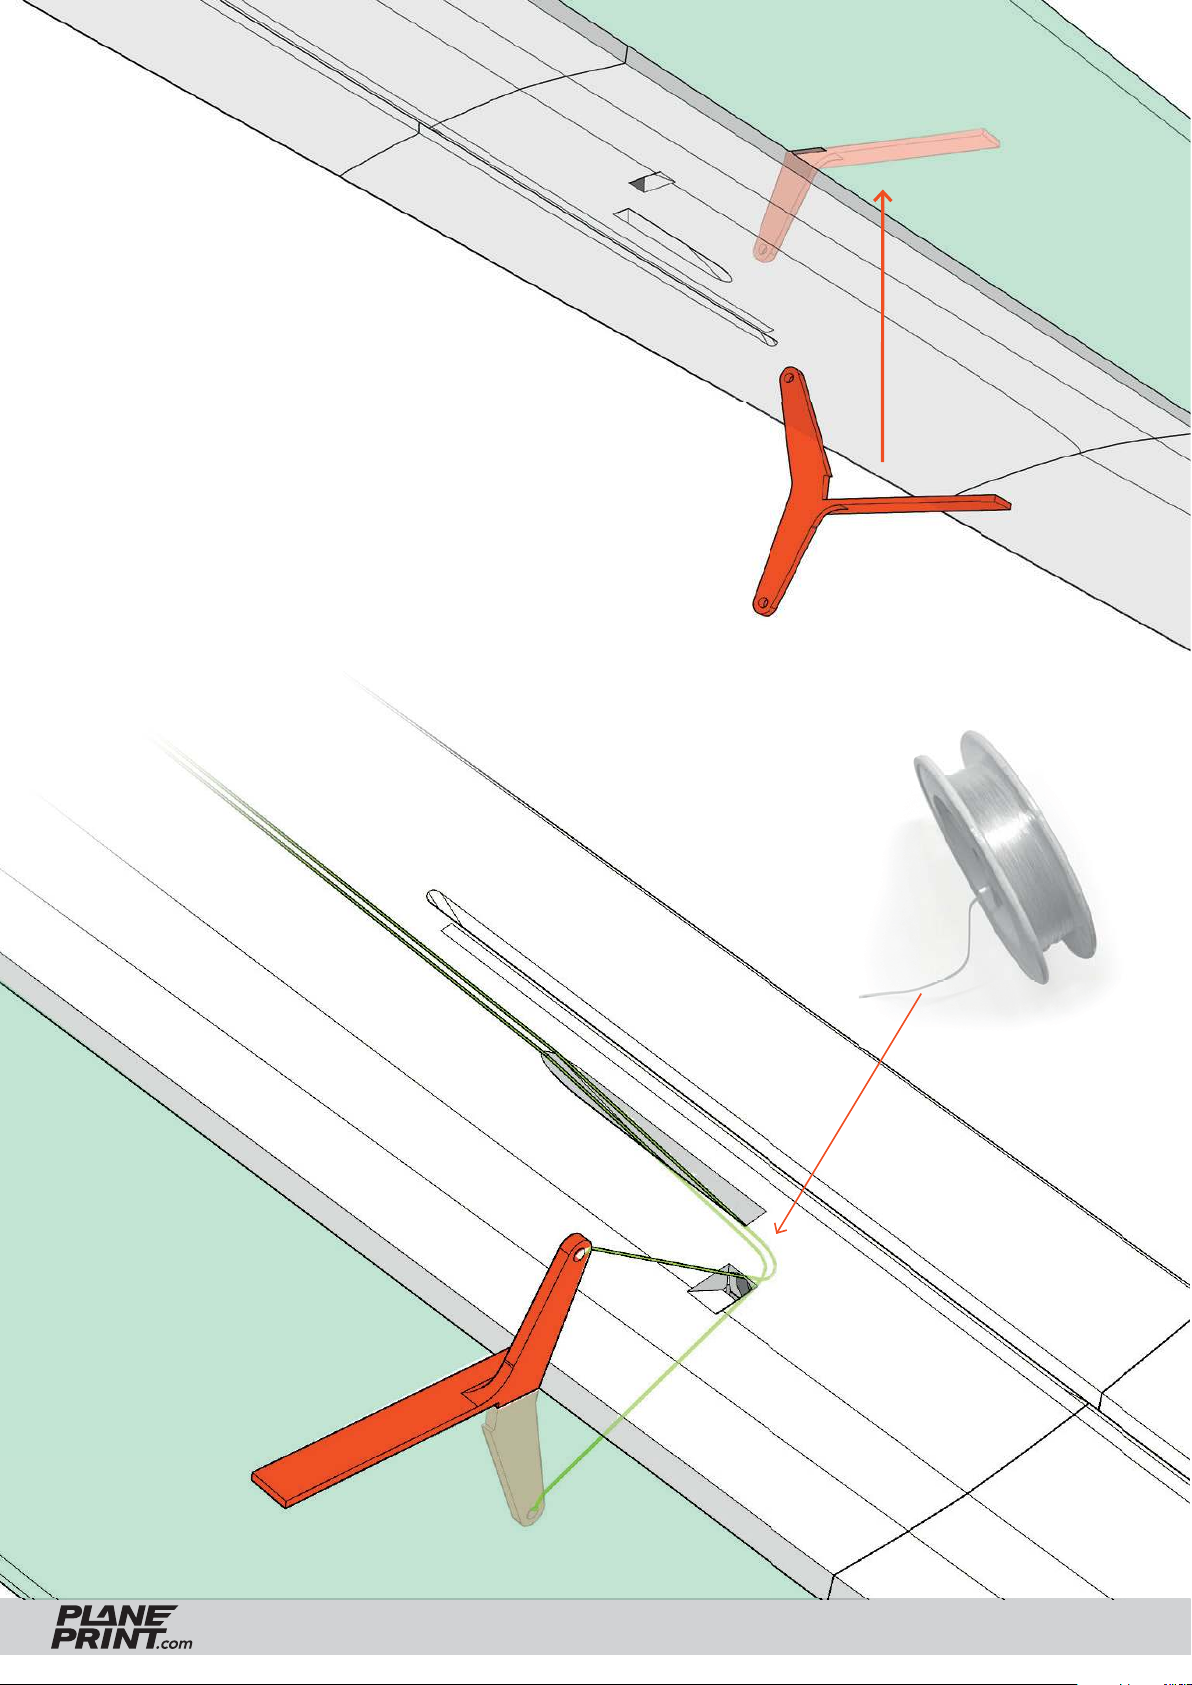
Aileron Servo mount
Glue the control horns to the underside of
the ailerons so that one half sticks out at the
bottom and one at the top. For Depron,
use UHU POR again as described above.
Now it gets a little tricky:
Cut a 1600 mm long piece of fi shing line and tie one
end to the lower horn of the Aileron. Then thread the
other end into the hole so that it comes out around
the bend below the wing.
Now thread the other end of the line into the wing in
the opposite direction from below. This must protrude
from the top and be tied to the upper horn.
P2_Parts 2–S1.stl
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
23
Page 24
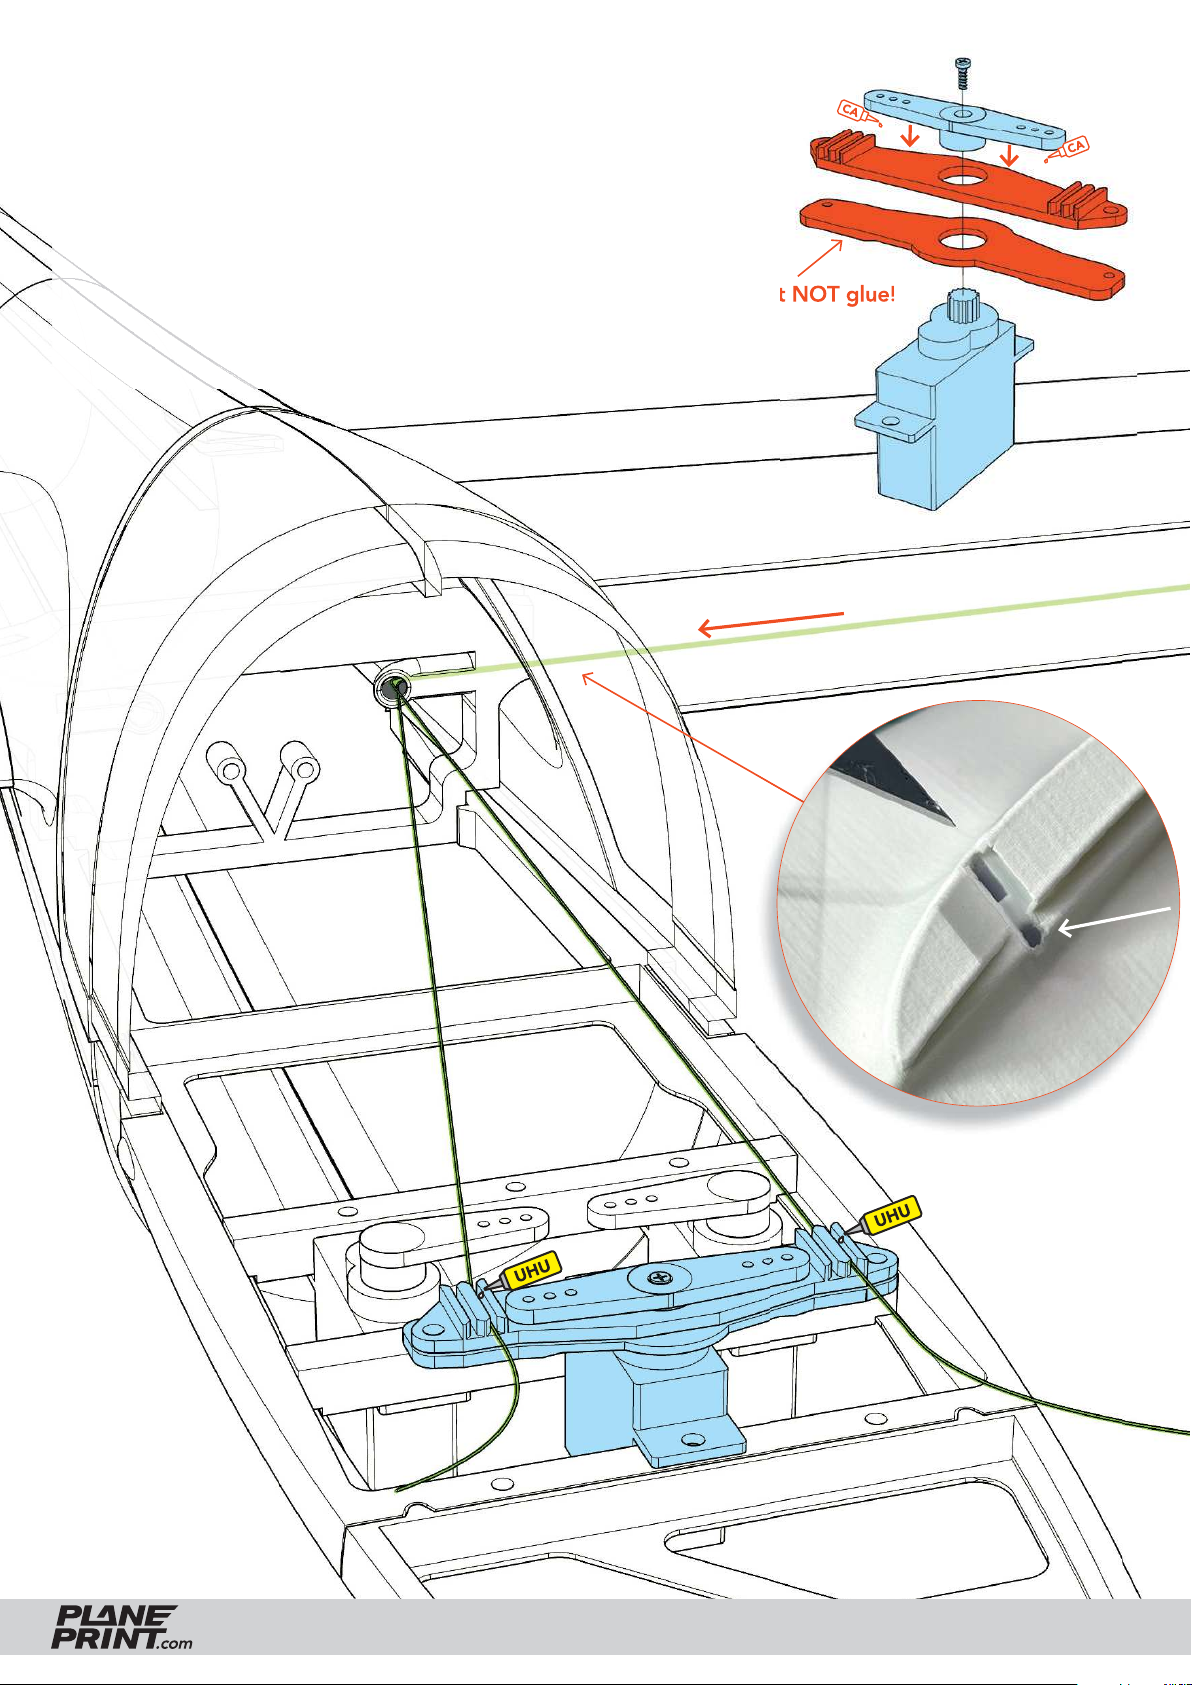
Aileron Servo mount
Set the aileron to neutral and gently tension the fi shing lines. Now
put a drop of UHU POR in the gap on the servo lever so that the
fi shing line runs in the glue and can also be pulled when the glue
is hard (therefore UHU and not CA glue). This way you can adjust
the tension later if necessary.
Then do this again in reverse with the other aileron.
When arranging the lines, make sure that the ailerons work in
opposite directions!
This part NOT glue!This part NOT glue!
Thread the
fi shing line here
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
24
Page 25
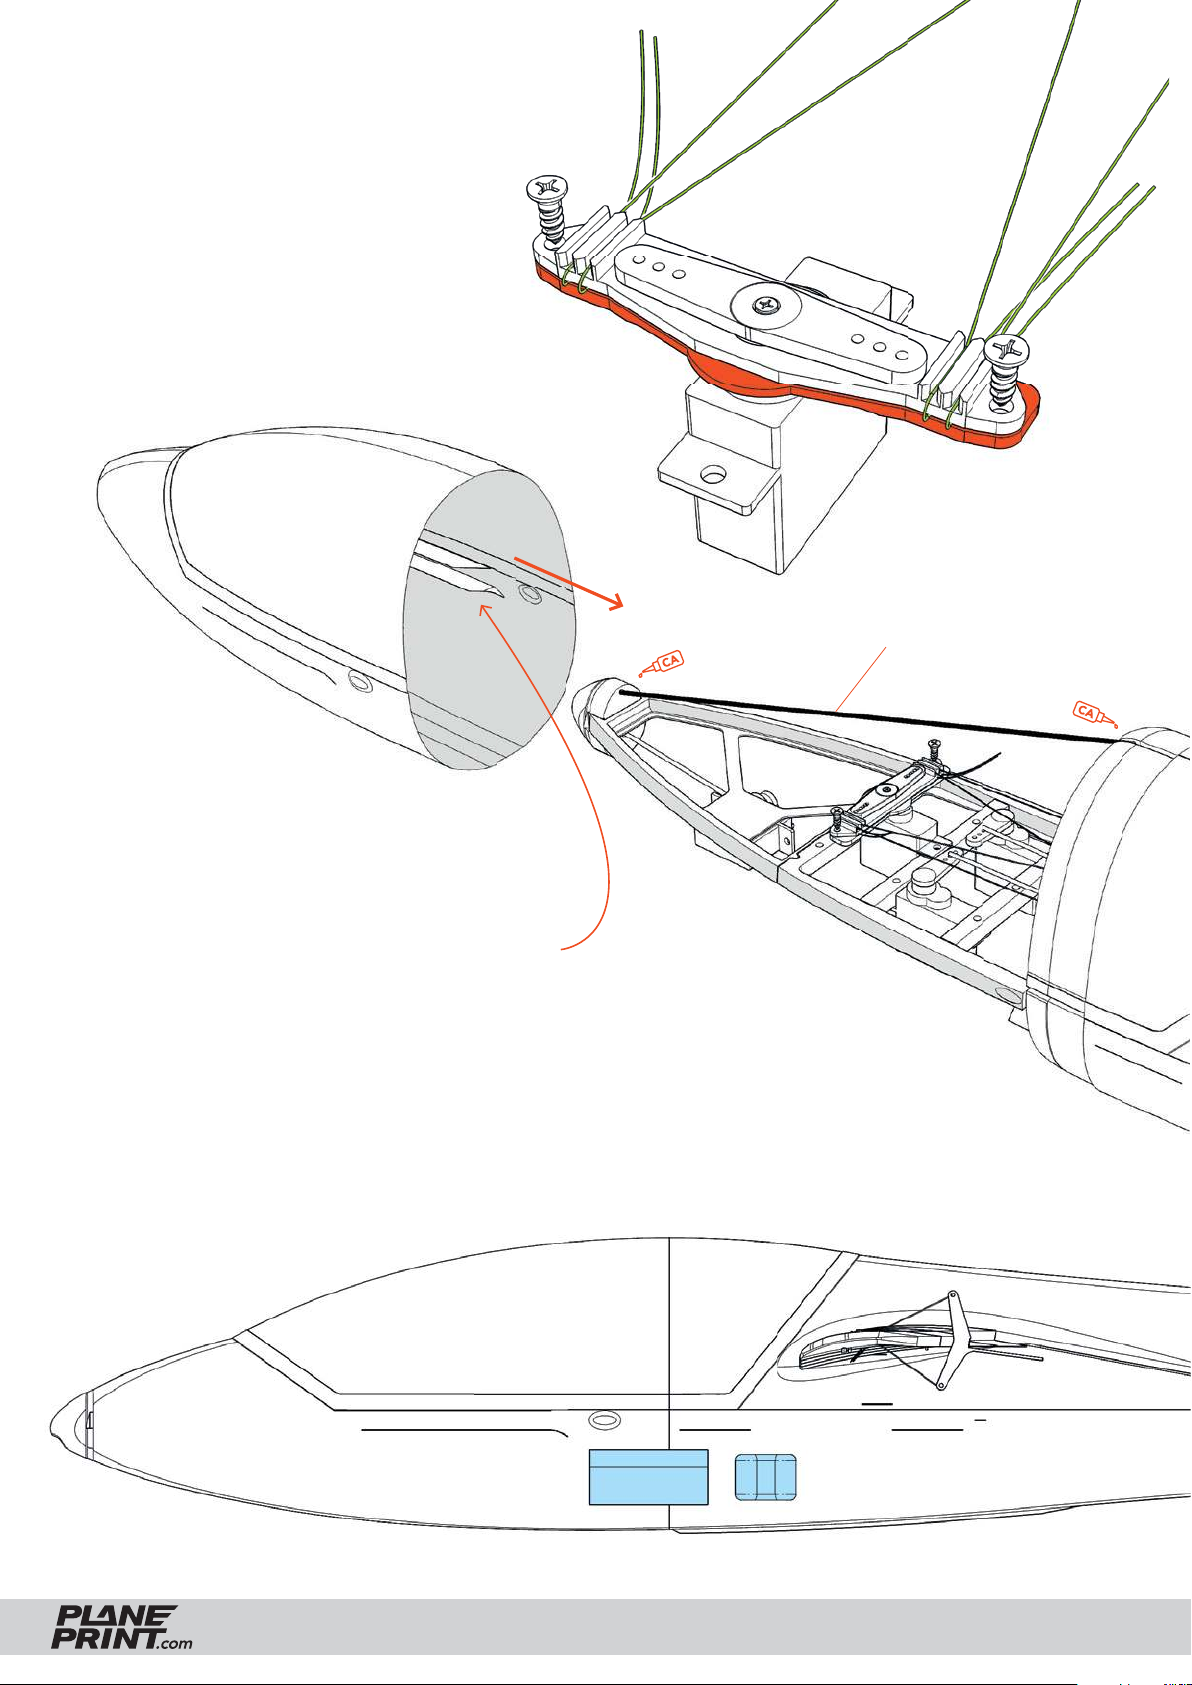
Aileron Servo mount
If the setting of the ailerons fi ts,
bend the fi shing lines downwards
and clamp them between the
plates. Then secure them with two
short screws. You can then change
the settings later.
V_Fuselage 1–S1.stl
Carbon rod Ø1*185 mm
Canopy
Glue in a piece of carbon rod for stabilization as shown
in the picture.
is not pushed up or down, otherwise the canopy
will no longer fi t exactly!
The canopy is simply pushed along the guide tabs
on the fuselage. It does not need to be fi xed in place.
Make sure that the tip (tow coupling)
RC Components
Position the components so that the CG fi ts exactly.
Secure them with self-adhesive Velcro tape.
SWIFT S1
BatteryReiceiver
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
25
Page 26
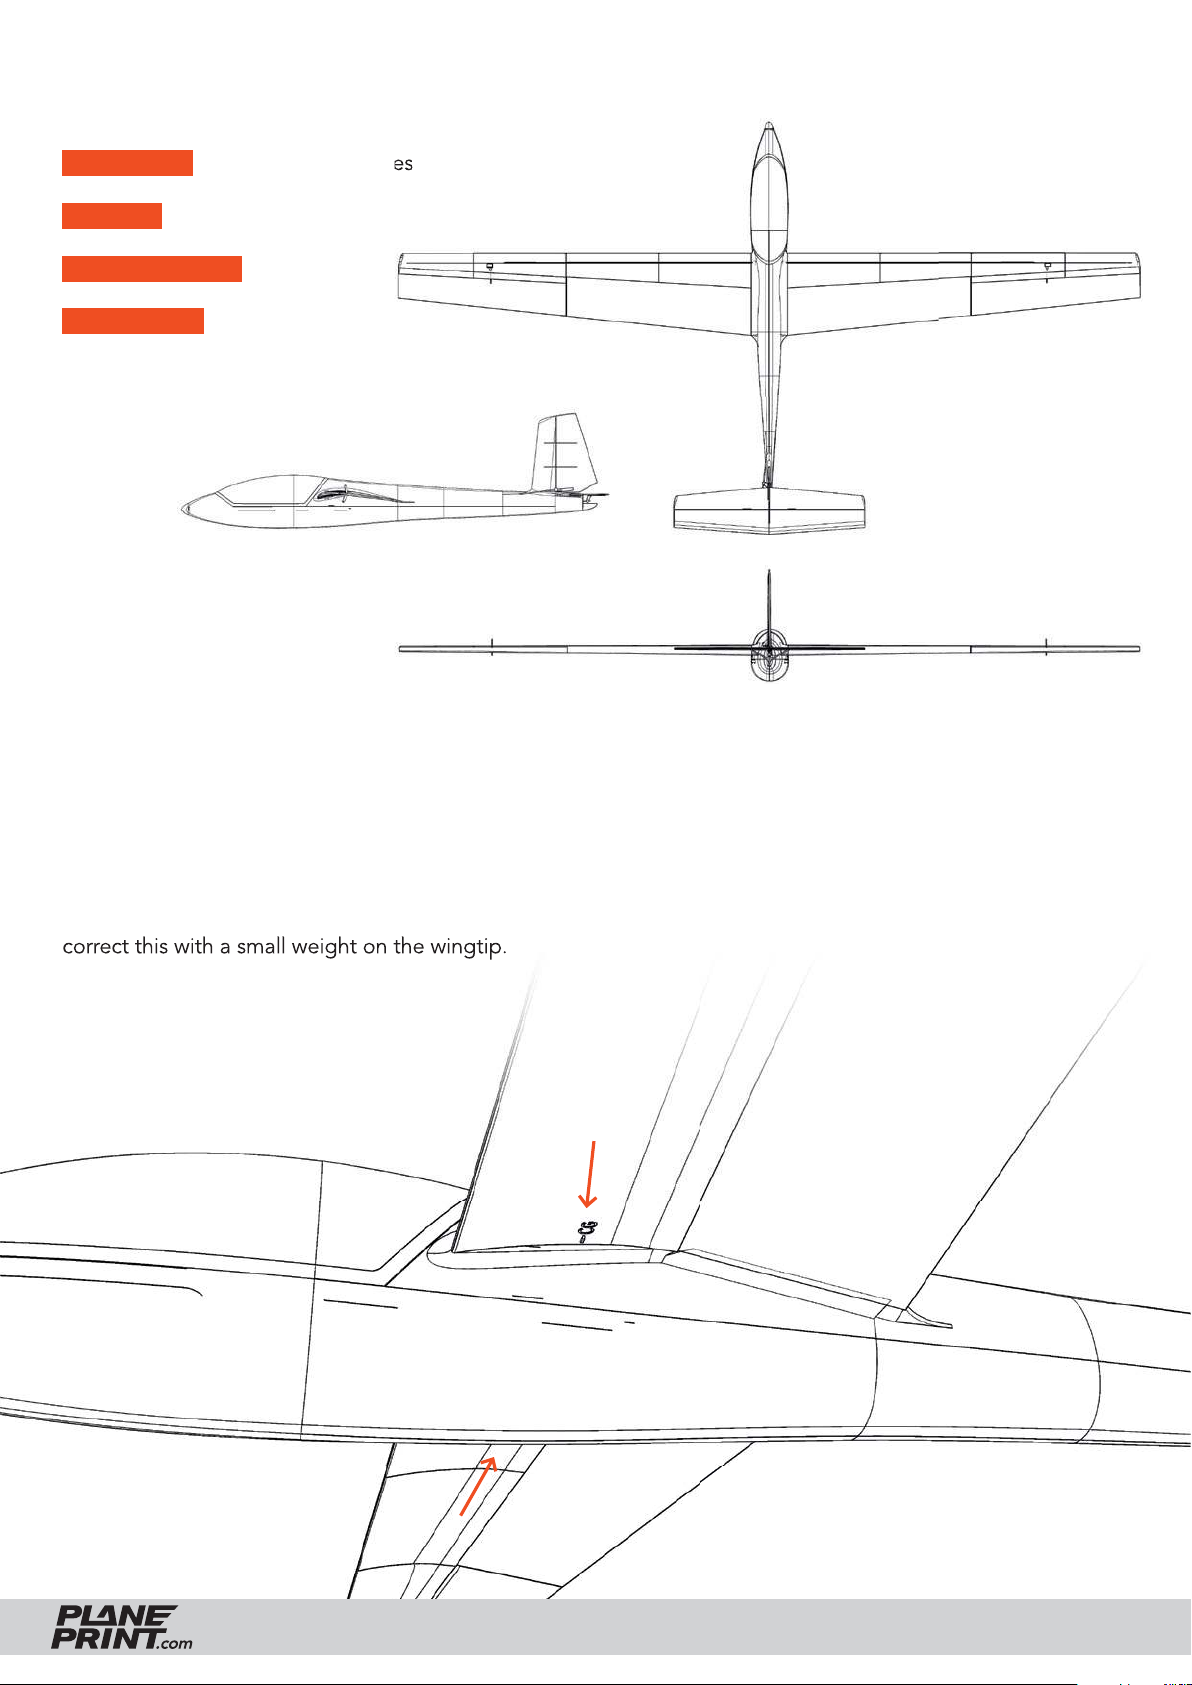
Technical specifi cations
WINGSPAN 1400 mm/55.1 inches
LENGTH 777 mm/30.6 inches
FLIGHT WEIGHT 190 grams
WING LOAD 10 g/dm
2
Center of Gravity (CG)
The aircraft must balance on these points –
(42 mm/1.6 inch behind the leading edge)
see the markings on the wing.
Do not forget to check if the wings are exactly in ballance in the roll axis. If one wing is heavier,
correct this with a small weight on the wingtip.correct this with a small weight on the wingtip.
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
26
Page 27
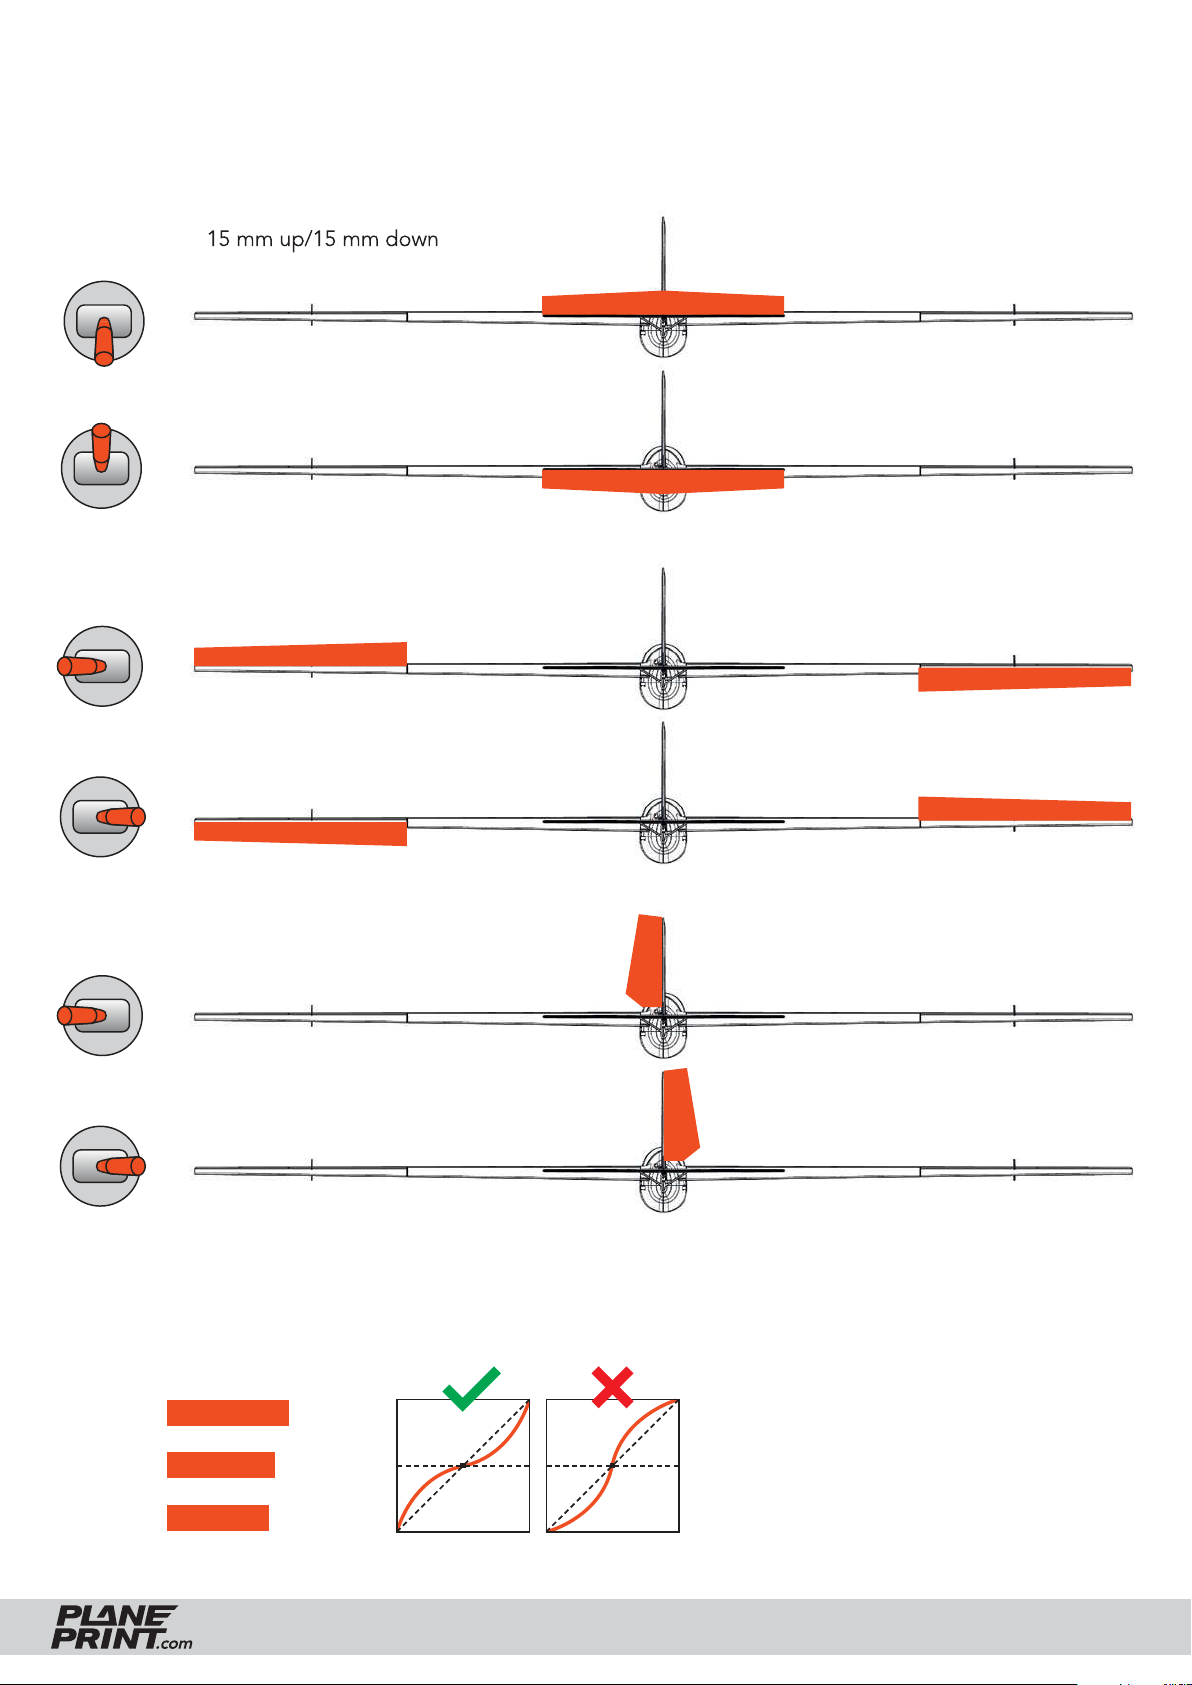
Control Direction Test
When checking the control directions, look at the aircraft from above (rudder) and behind.
ELEVATOR 15 mm up/15 mm down
AILERON 15 mm up/15 mm down
RUDDER 30 mm left/30 mm right
Program the throttle lever or a switch for the Tow function.
EXPO
ELEVATOR 30 %
AILERON 30 %
RUDDER 30 %
(for some remote
controls a minus
has to be in front
of the number)
SWIFT S1
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
27
Page 28
AGE RECOMMENDATION 14+
NOT FOR CHILDREN UNDER 14 YEARS.
THIS IS NOT A TOY!
The STL data (or data processed from it, such as G codes)
must never be passed on to third parties!
The purchase of the STL does not authorize the production
of models for third parties.
By using the download data, an RC model airplane, called
„model“ for short, can be manufactured using a 3D printer.
As a user of this model, only you are responsible for safe
operation that does not endanger you or others, or that
does not damage the model or property of others.
PLANEPRINT.com assumes no responsibility for damage to
persons and property caused by pressure, transport or use
of the product. Filaments, printing supplies, hardware or
consumables that can not be used after faulty 3D printing
will not be replaced by PLANEPRINT.com in any way.
When operating, always keep a safe distance from your
model in all directions to avoid collisions and injuries.
This model is controlled by a radio signal. Radio signals can
be disturbed from outside without being able to influence
it. Interference can lead to a temporary loss of control.
Always operate your model on open terrains, far from cars,
traffic and people.
Keep all chemicals, small parts and electrical components
out of the reach of children.
Avoid water contact with all components that are not specially
designed and protected. Moisture damages the electronics.
Never take an item of the model or accessory in your mouth
as this can lead to severe injuries or even death.
Never operate your model with low batteries in the transmitter or model.
Always keep the model in view and under control.
Use only fully charged batteries.
Always keep the transmitter switched on when the model
is switched on.
Always remove the battery before disassembling the model.
Keep moving parts clean and dry at all times.
Always allow the parts to cool before touching them.
Always remove the battery after use.
Make sure that the Failsafe is properly set before the flight.
Always follow the instructions and warnings for this product
and any optional accessories (servos, receivers, motors,
propellers, chargers, rechargeable batteries, etc.) carefully.
We develop our models to the best of our knowledge and belief.
We accept no liability for consequential damage and injuries
caused by improper use or incorrectly printed parts. Please be
careful when handling motors, batteries and propellers and
only move your model with insurance and in approved places!
Never operate the model with damaged wiring.
Never touch moving parts.
© PLANEPRINT.com, A-6021 Innsbruck, Conradstraße 6, [email protected]
© Design STL files by René Marschall • Layout: marschall designlab, marschall.cc
 Loading...