

Page 1
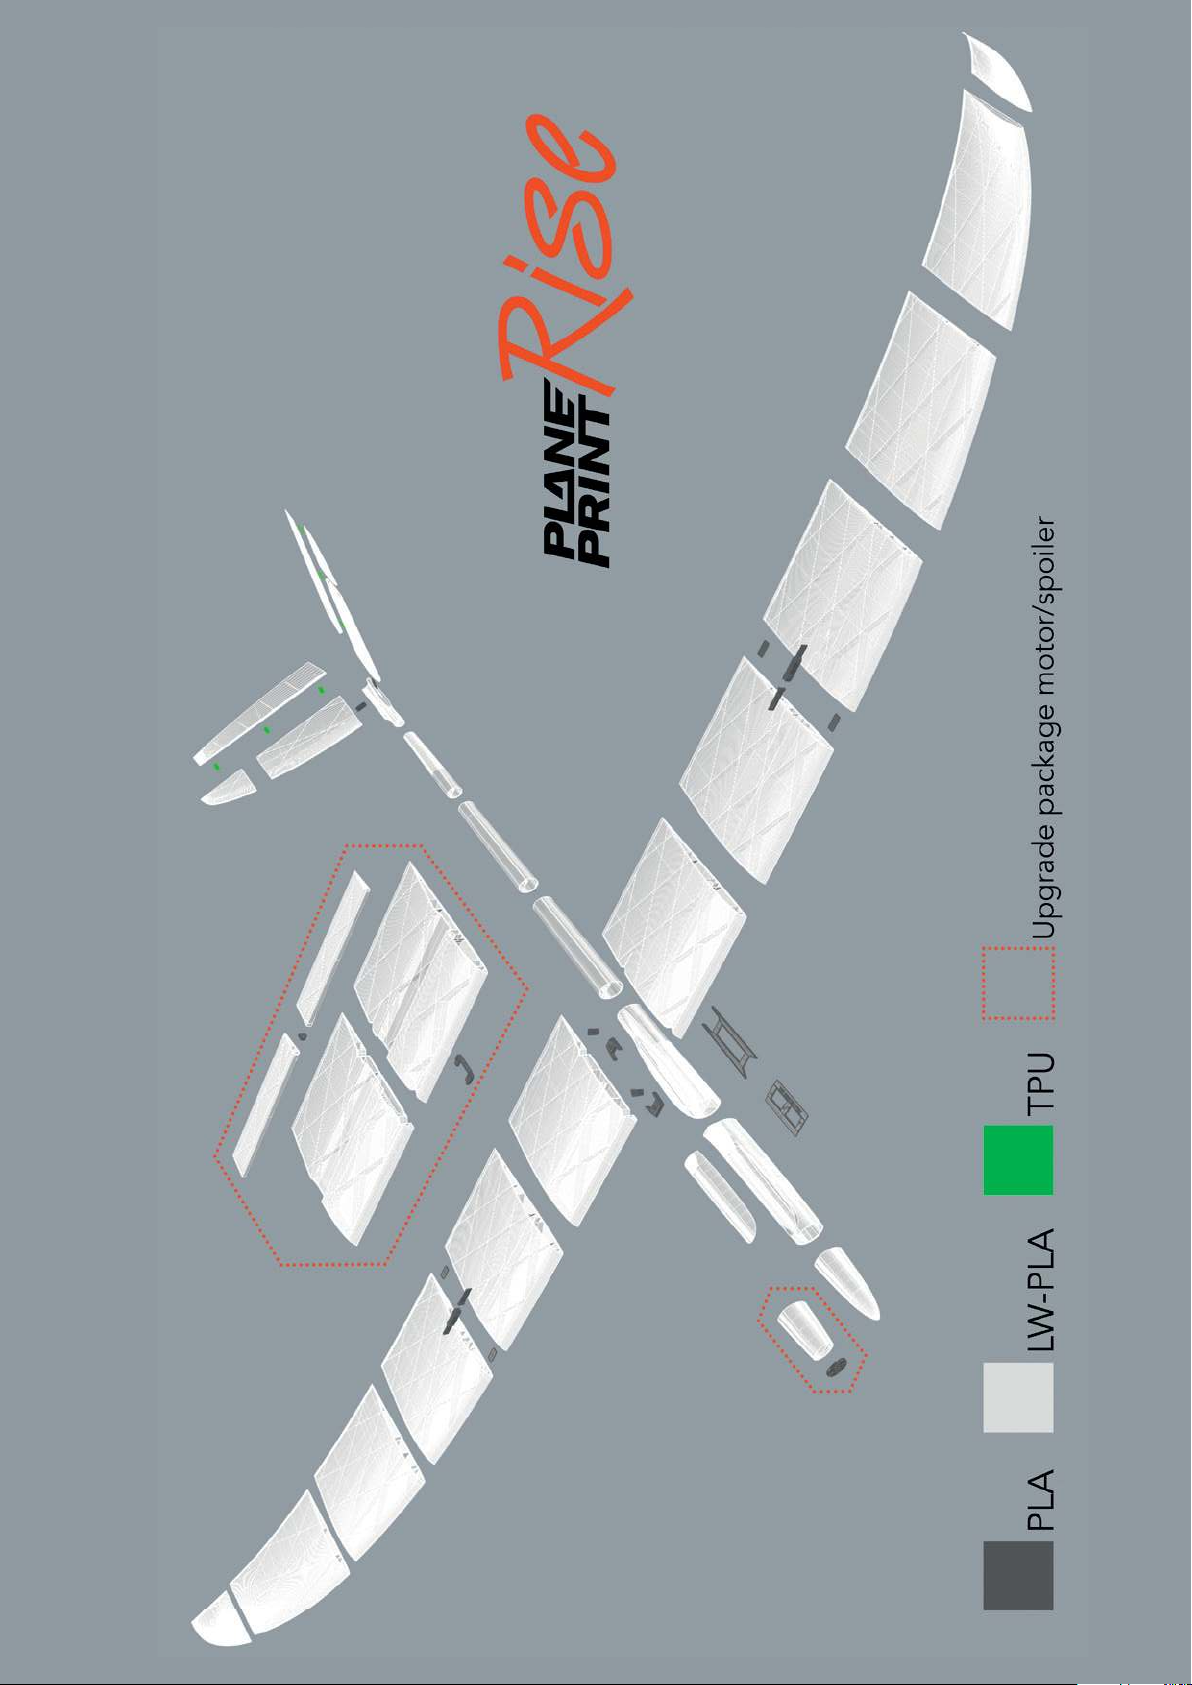
RISE Glider version and Motor/Spoiler upgrade Kit
NOTE: Slicing only
works with CURA!
You can fi nd the STL data
at www.planeprint.com
PRINTING & ASSEMBLING MANUAL
Page 2
PRINTING THE PARTS – PRINTING PROFILES
You may wonder why this 3D model is exclusive to CURA?
The most important thing with small RC model airplanes is always the size to weight ratio. The
lighter a model is, the better its flight characteristics and also the flight time is significantly increased.
With our unique design process, we manage to offer weight-relevant parts in a true 1-wall printing
process for both the outer skin and the filling. This allows us to save weight while maintaining the
necessary stability.
Here we show you how to make adjustments from a standard CURA profile. For this model we need
only 4, easy to create profiles.
It is important to follow the instructions from PLANEPRINT.com to slice the part correctly.
However, it can be useful to perfect your 3D printing by making some additional settings depending
on the printer and filament used.
For slicing all Planeprint
models, four profiles have
to be created in Cura:
PROFILE P1_fullbody
PROFILE P2_hollowbody
PROFILE P3_surface
PROFILE P4_flex
You can find the description at
www.planeprint.com/print
IMPORTANT FOR
THE 1-WALL-PRINT!
In order to print airfoils of the lowest possible weight with high stability, it is necessary to print with only one wall line (Nozzle 0.4
mm). Decisive here is the adhesion between
the layers! To achieve this, you must print at
a much higher temperature than normal. As
a guideline, 230 ° C is a good starting point.
The parts-cooling fan should be set to 0% or
a maximum of 20%. Since not every printer
works the same, it may be necessary to make
small adjustments to these settings.
The development of a complex, airworthy RC flight model to express on any standard 3D printer is
a very complex and extensive process. Therefore, we appeal to your fairness not to forward the STL
data you have acquired to third parties. Our STL files are provided with indelible copyright watermarks that can be verified at any time.
Thank you for your understanding and have fun with your PLANEPRINT MODEL!
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
2
Page 3
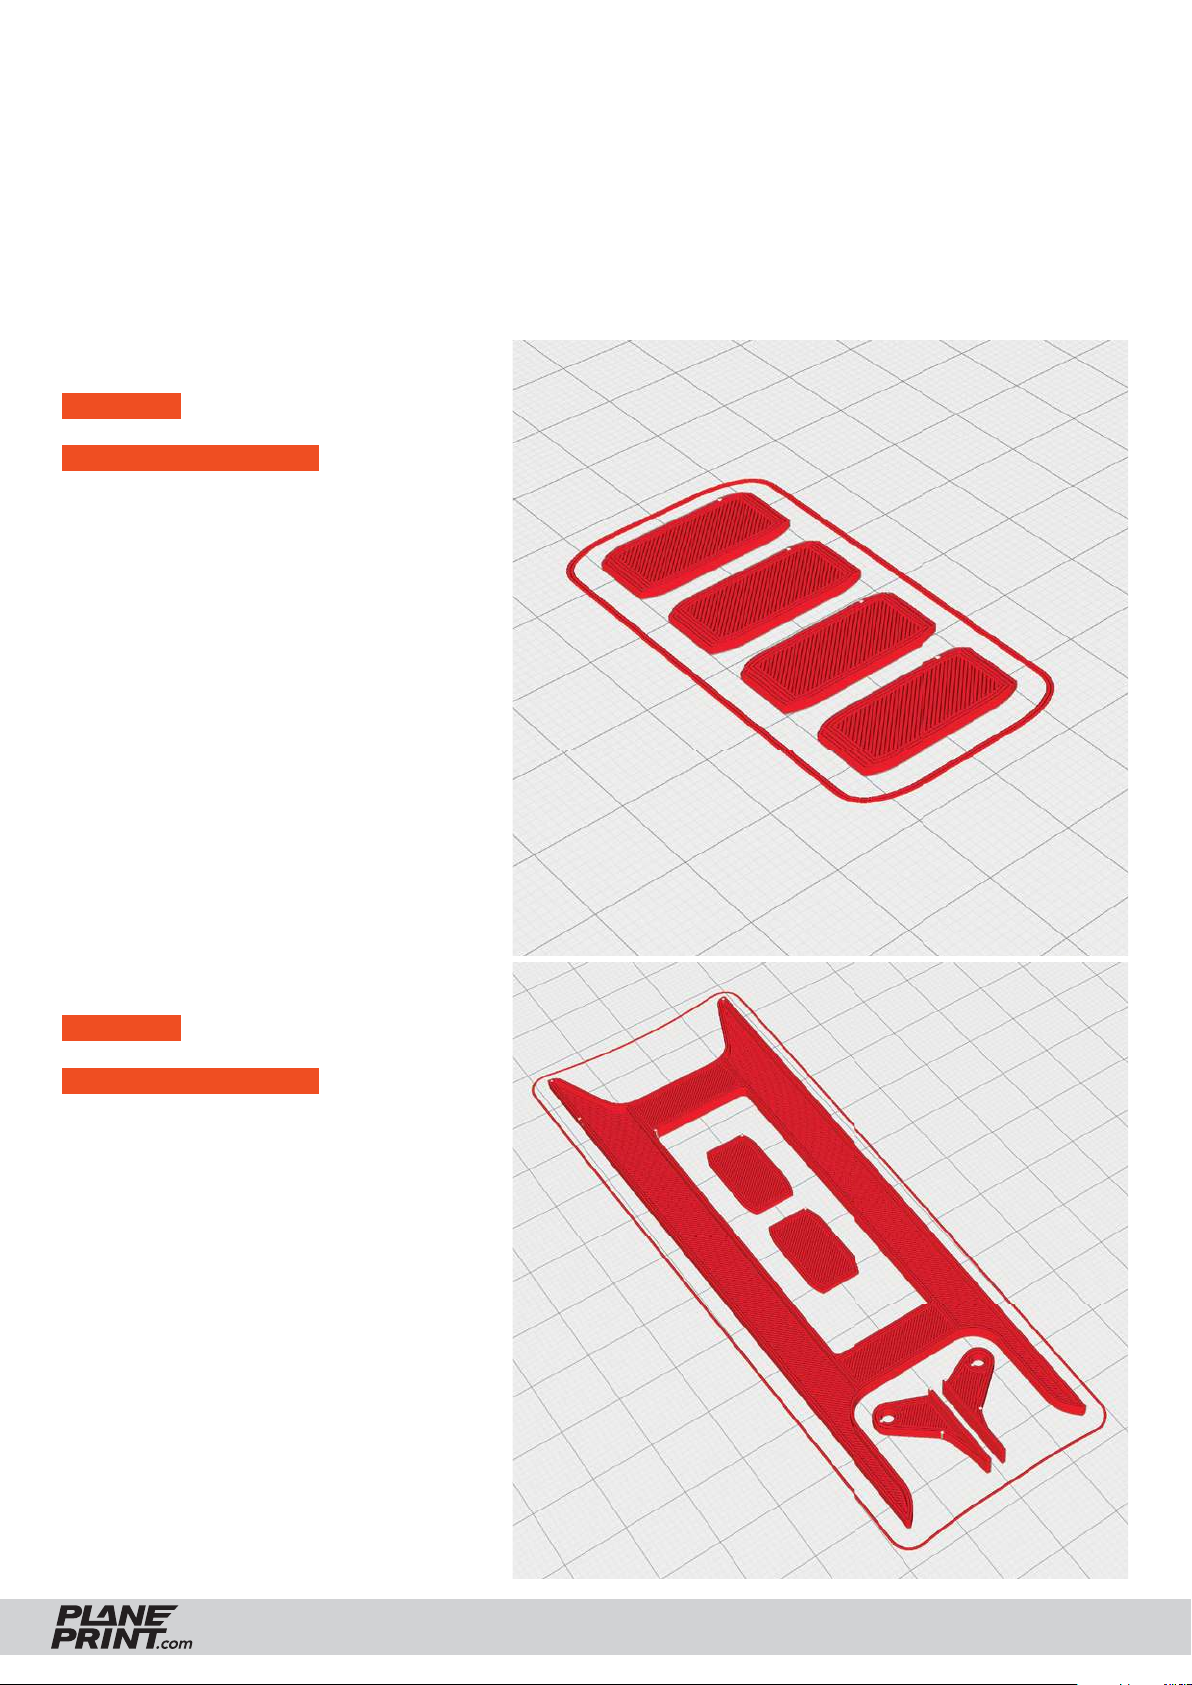
PROFILE P1_FULLBODY normal PLA
The following parts must be sliced with the PROFILE P1_FULLBODY.
Please note the additional settings for the individual parts!
Interconnects_profi le1_rise.stl
MATERIAL PLA, Weight: ~ 1 g
ADDITIONAL SETTINGS
None required
Parts_profi le1_rise.stl
MATERIAL PLA, ~ 4 g
ADDITIONAL SETTINGS
None required
There are several versions to choose from:
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
3
Page 4
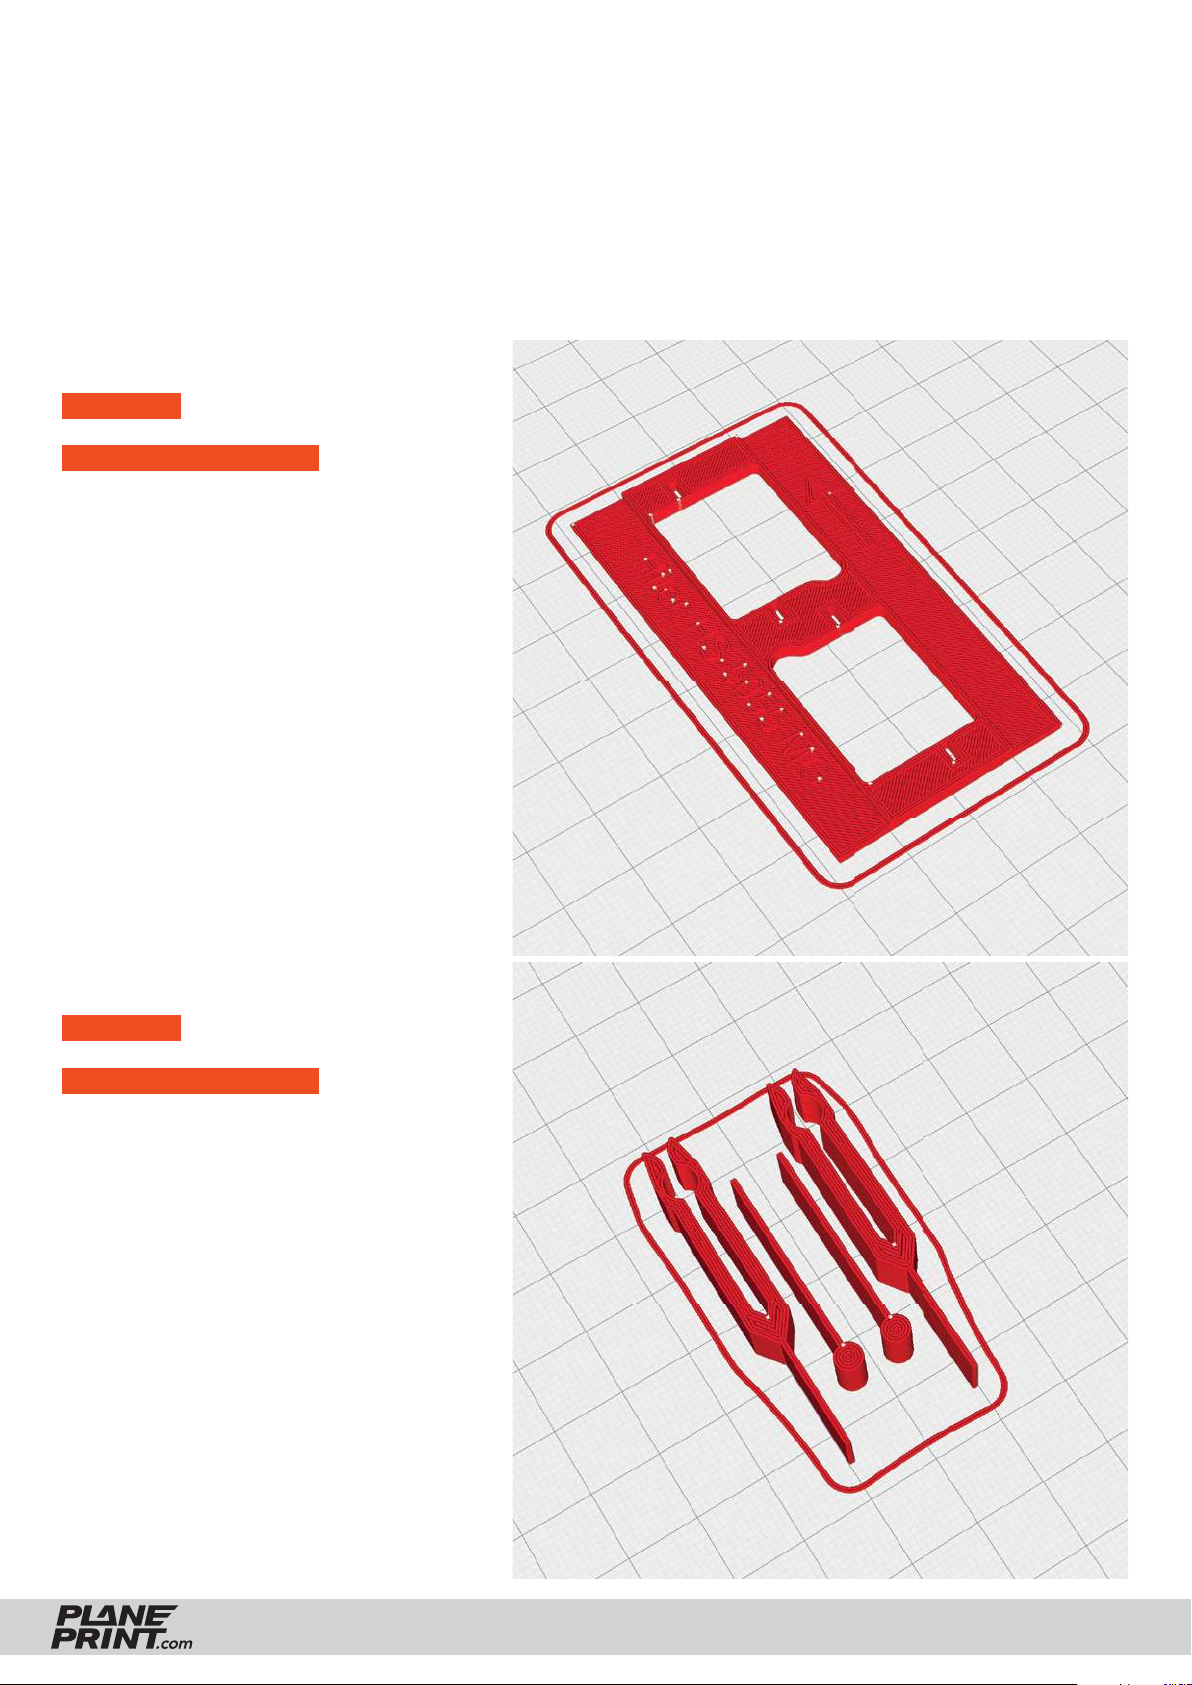
PROFILE P1_FULLBODY normal PLA
The following parts must be sliced with the PROFILE P1_FULLBODY.
Please note the additional settings for the individual parts!
Servomount_xxx_profi le1_rise.stl
MATERIAL PLA, ~ 3 g
ADDITIONAL SETTINGS
None required
Snap lock_profi le1_rise.stl
MATERIAL PLA, ~ 4 g
ADDITIONAL SETTINGS
• Wall Line Count: 6
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
4
Page 5
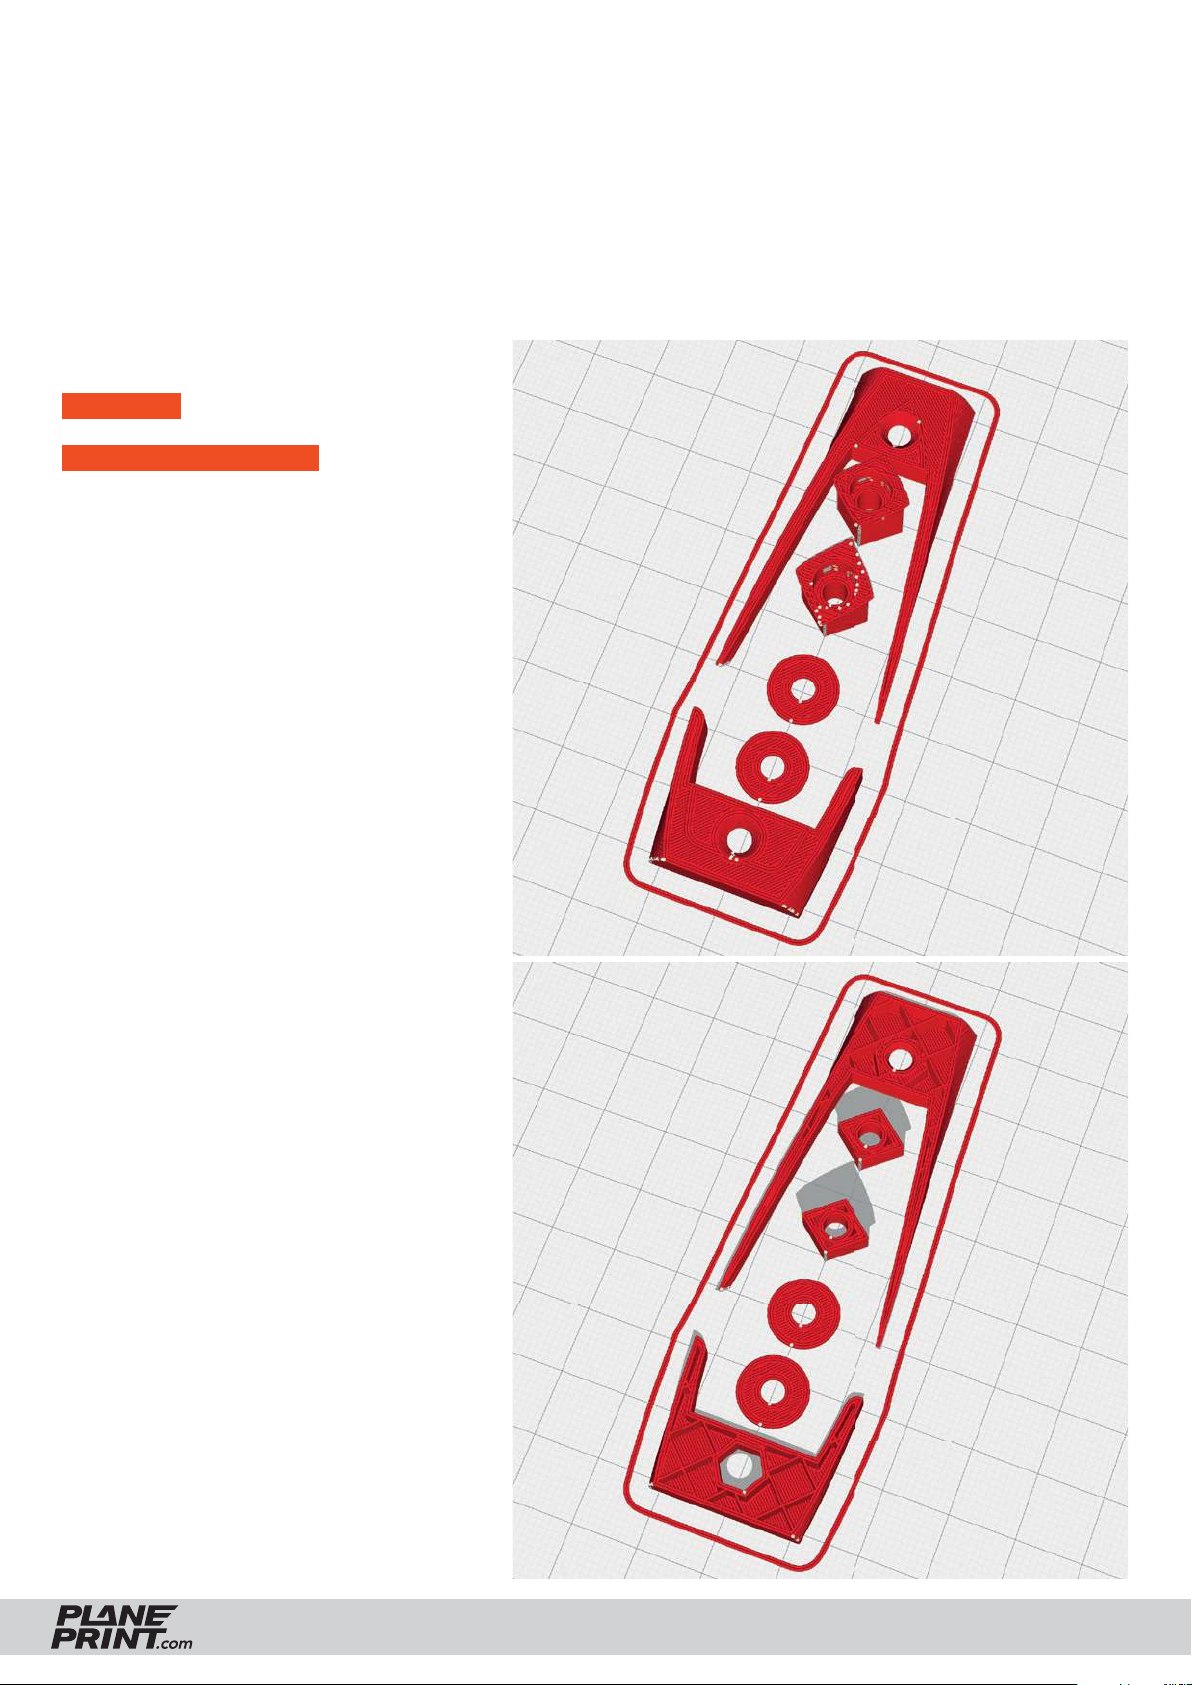
PROFILE P2_HOLLOWBODY normal PLA
The following parts must be sliced with the PROFILE P2_HOLLOWBODY.
Please note the additional settings for the individual parts!
Wingmount_profi le2_rise.stl
MATERIAL PLA, ~ 4 g
ADDITIONAL SETTINGS
None required
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
5
Page 6
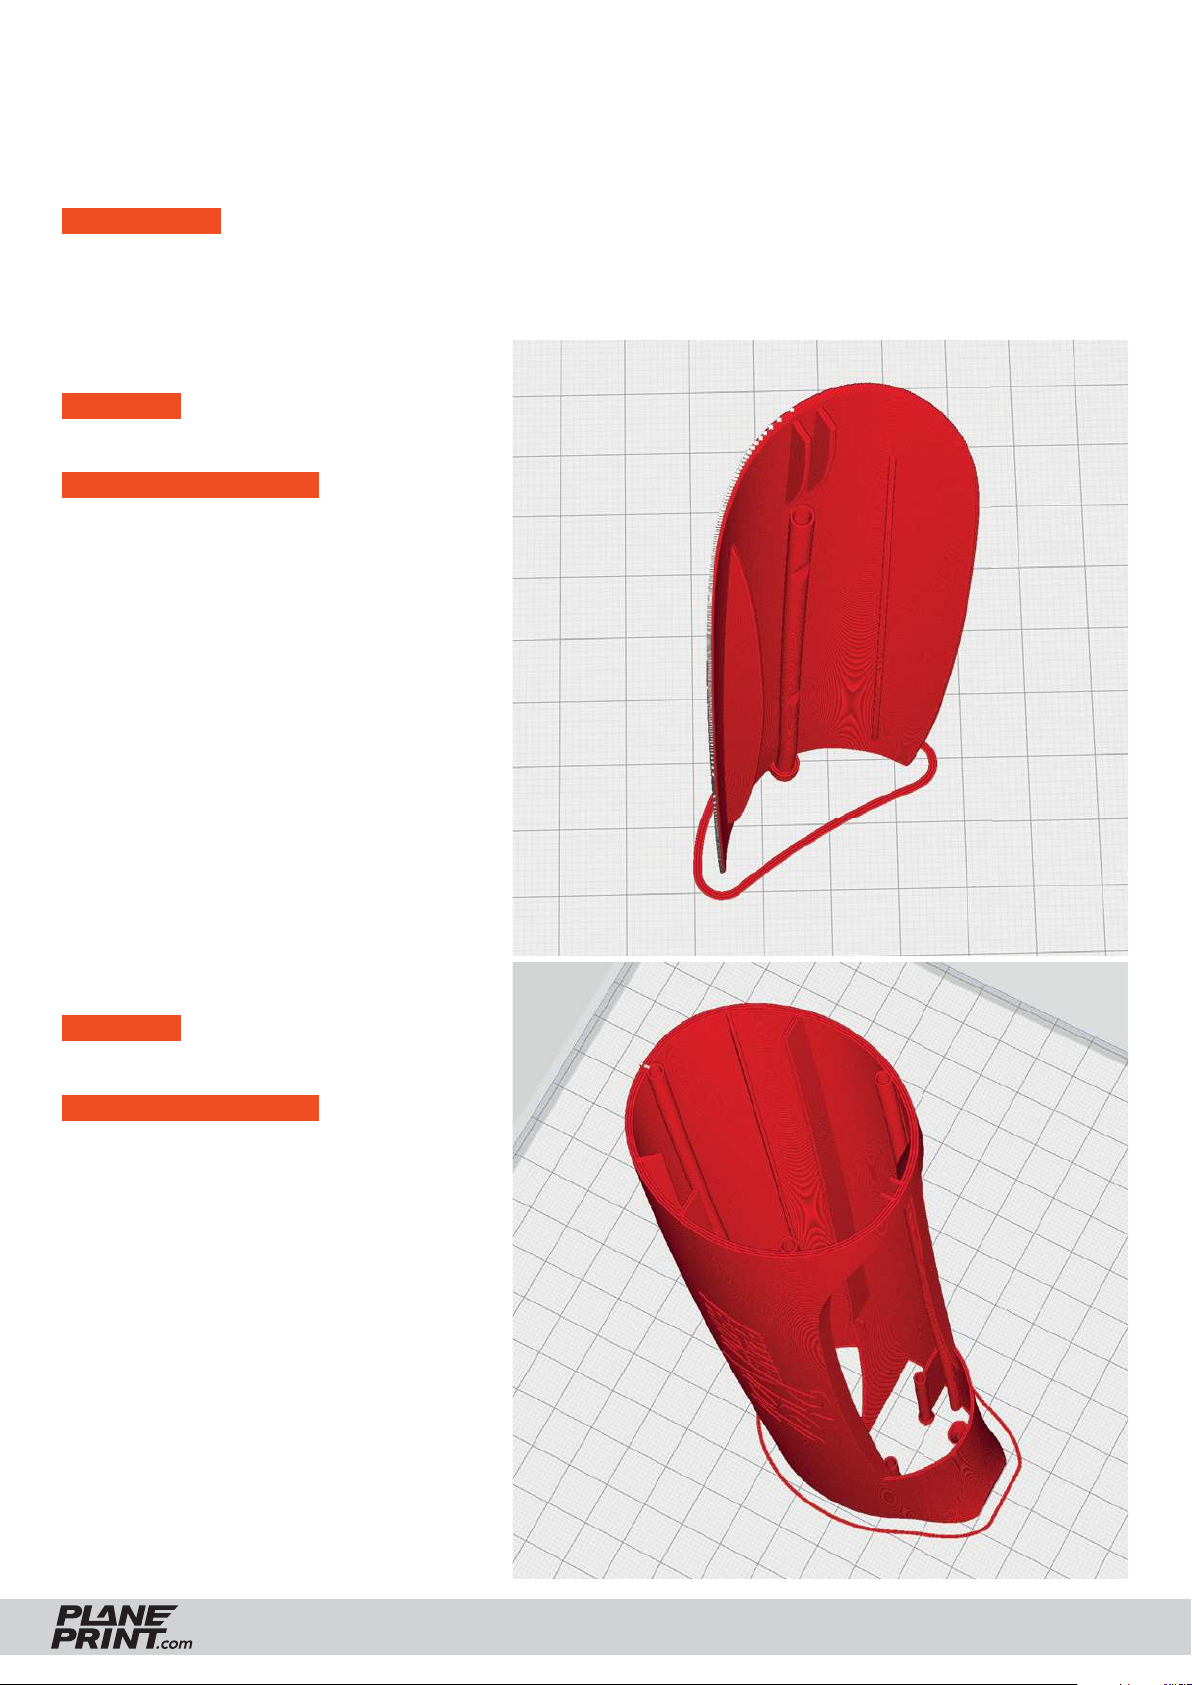
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
Canopy LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 7 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Fuselage1 LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 30 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
6
Page 7
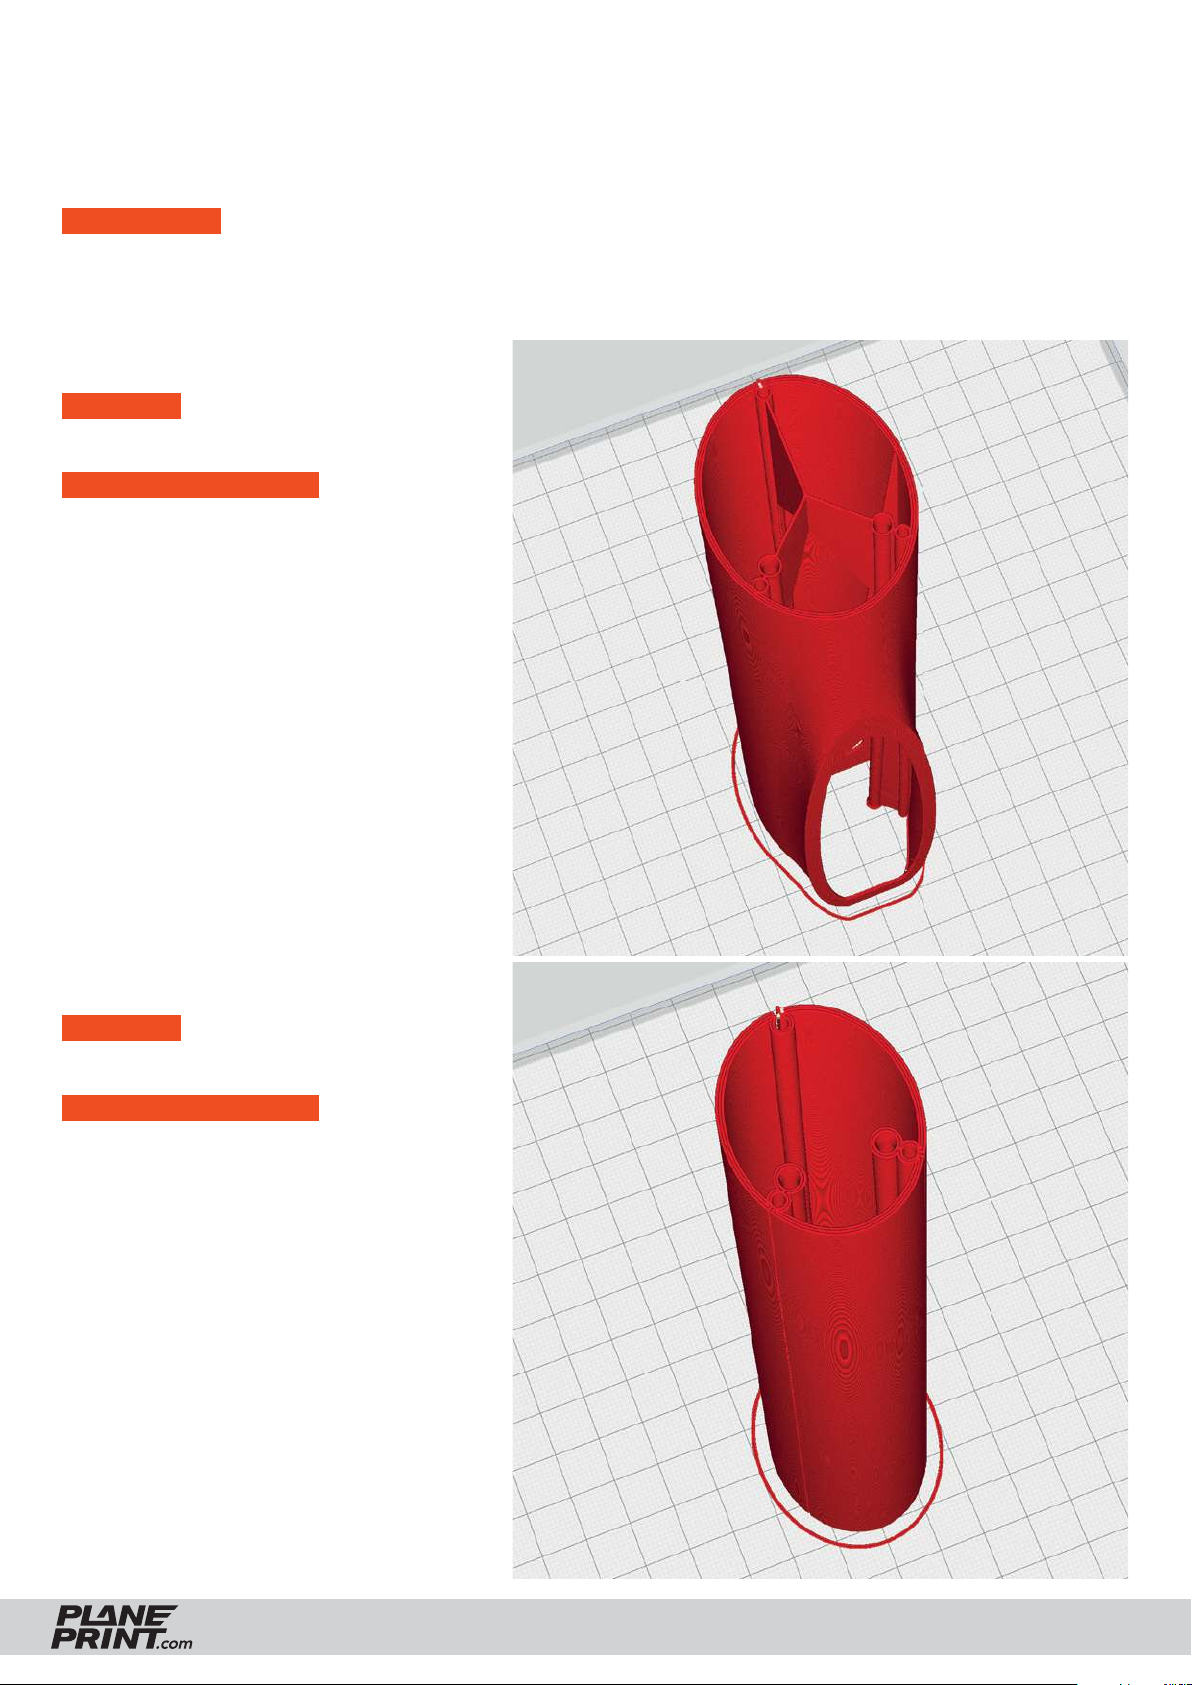
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
Fuselage2 LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 34 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Fuselage3 LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 29 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
7
Page 8
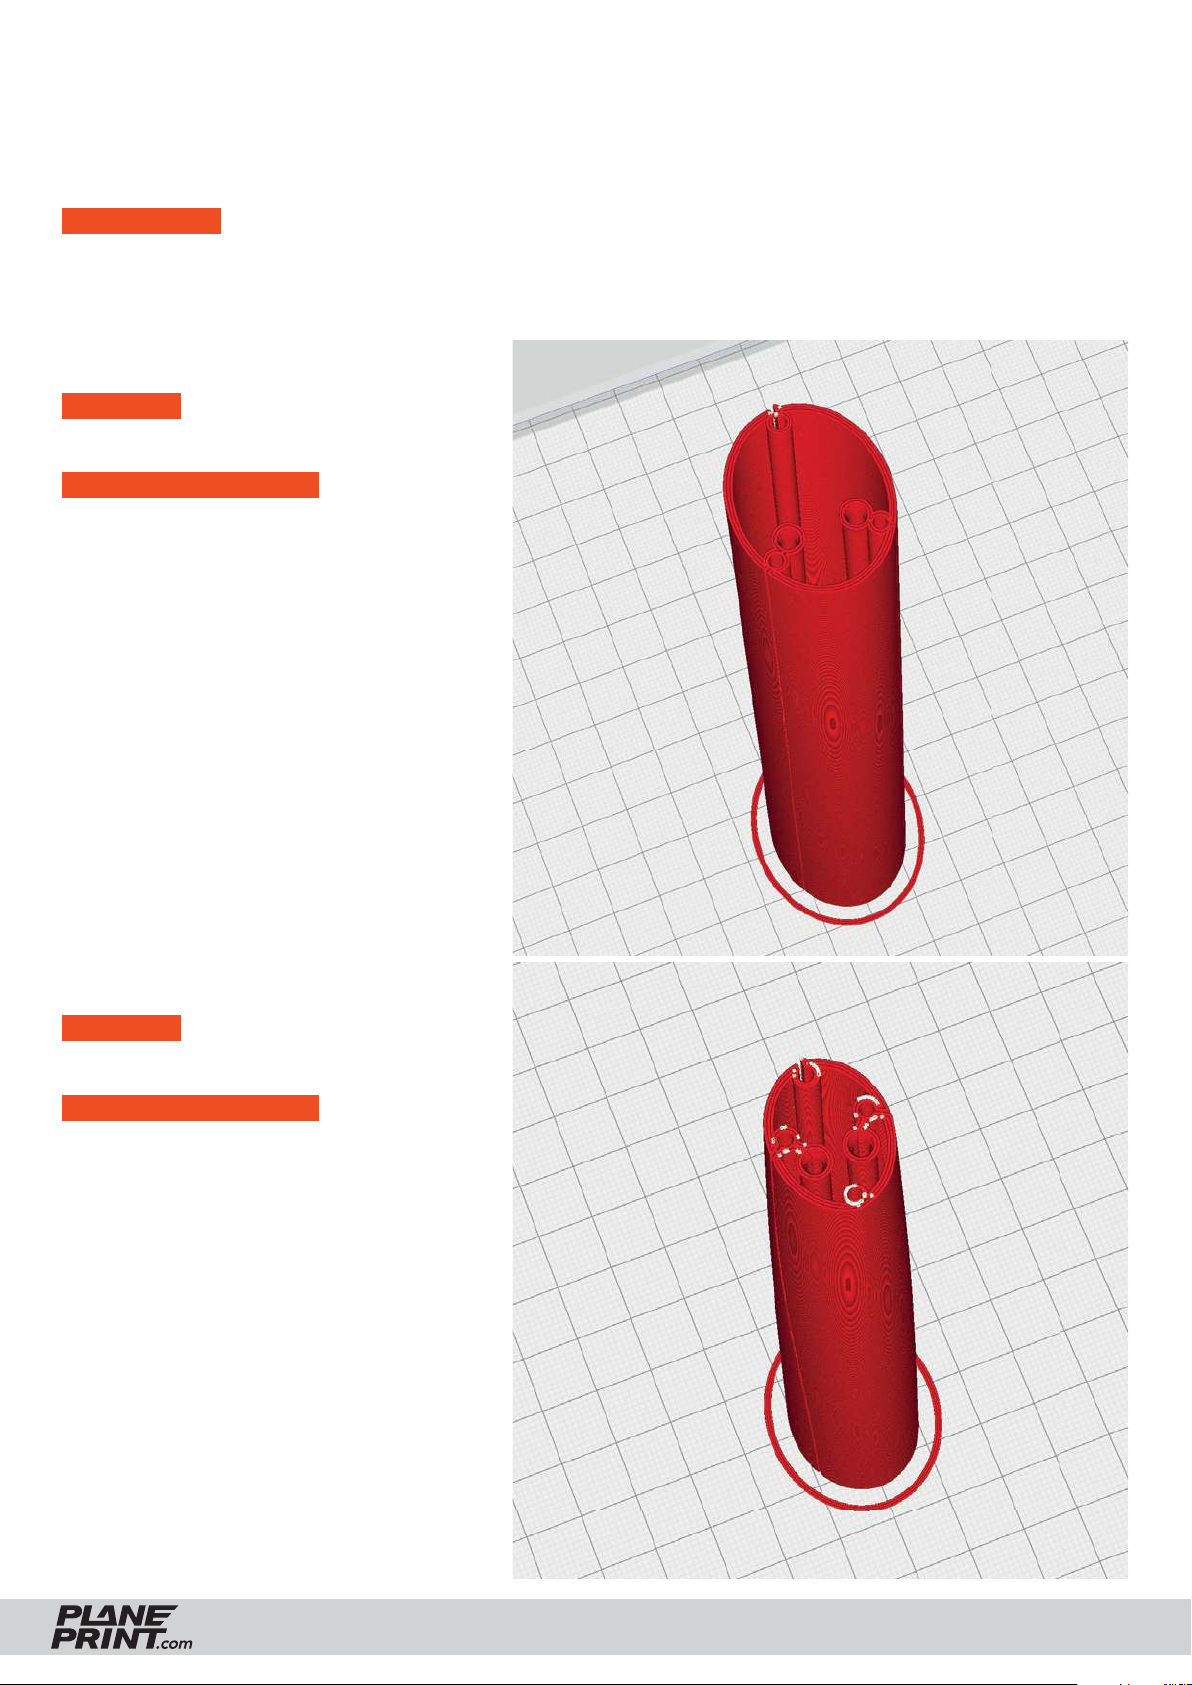
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
Fuselage4 LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 25 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Fuselage5 LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 18 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
8
Page 9
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
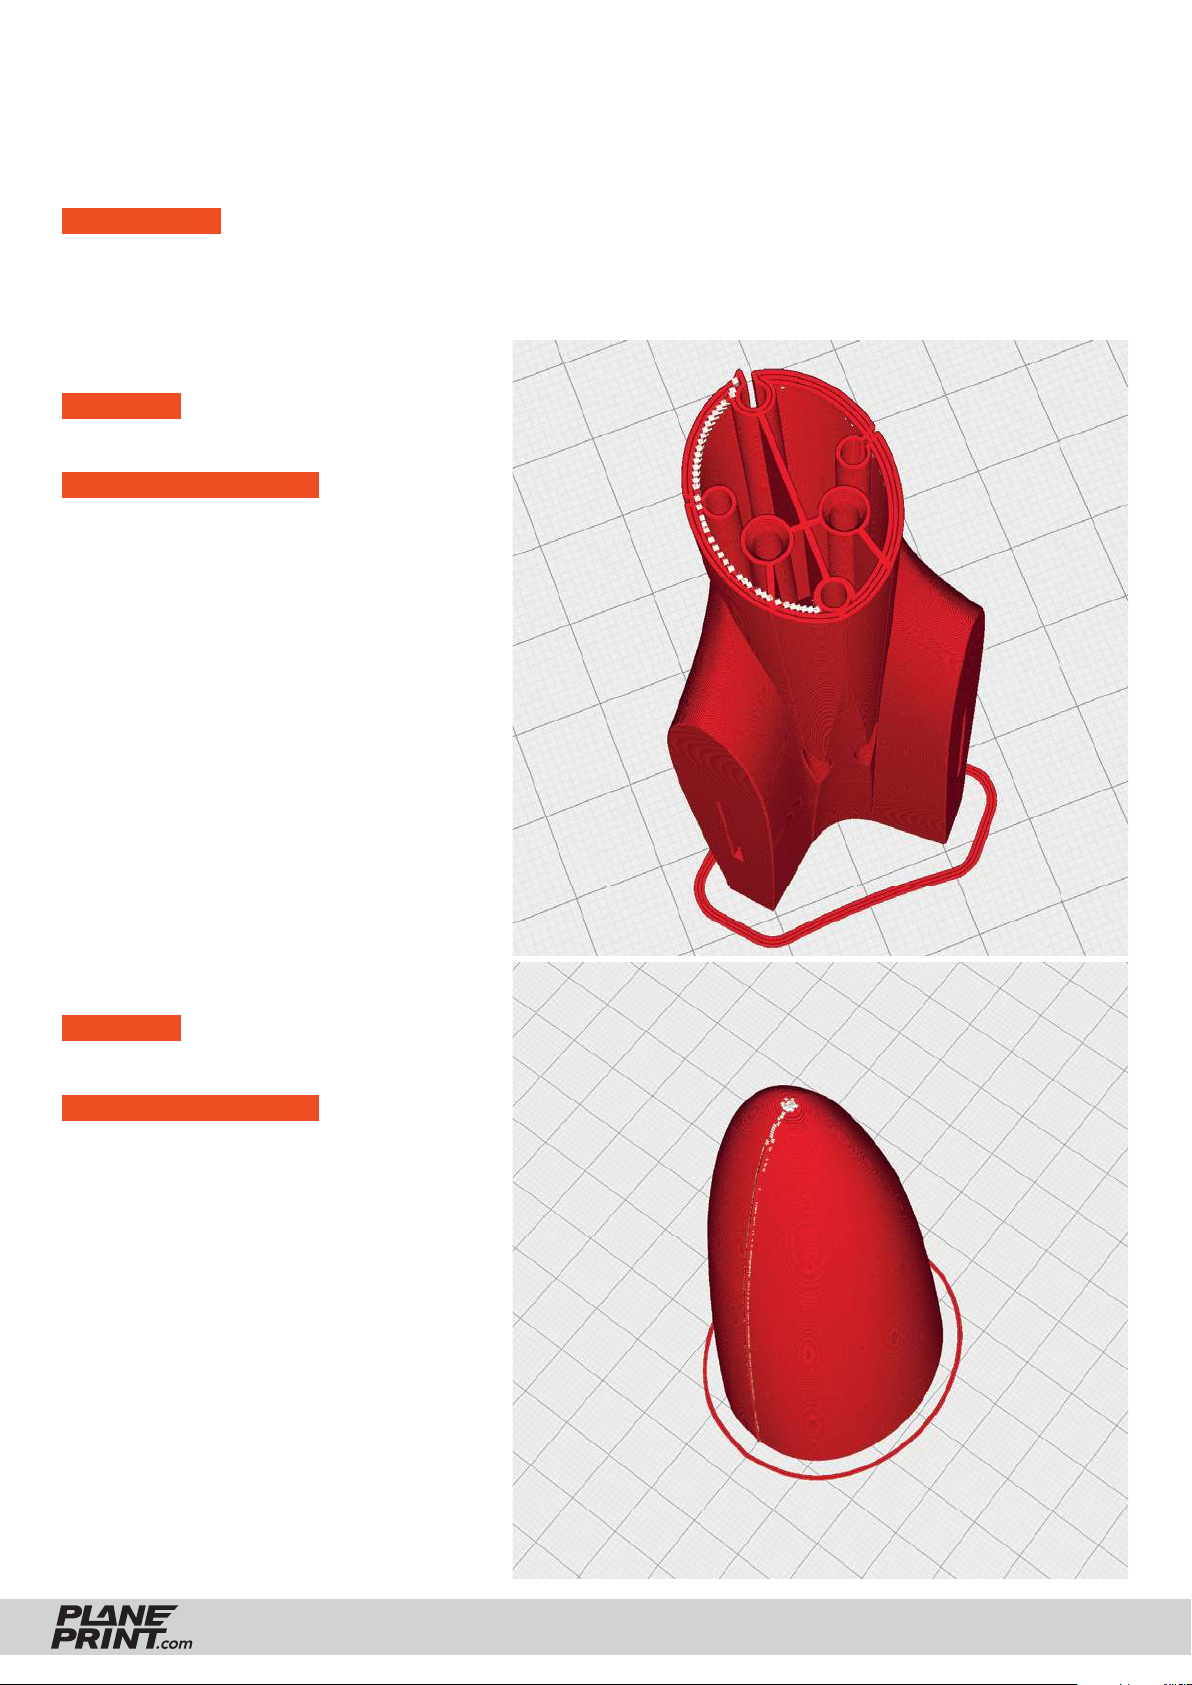
Fuselage6 LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 8 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
• Fan +30 %
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Nose LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 11 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
9
Page 10
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
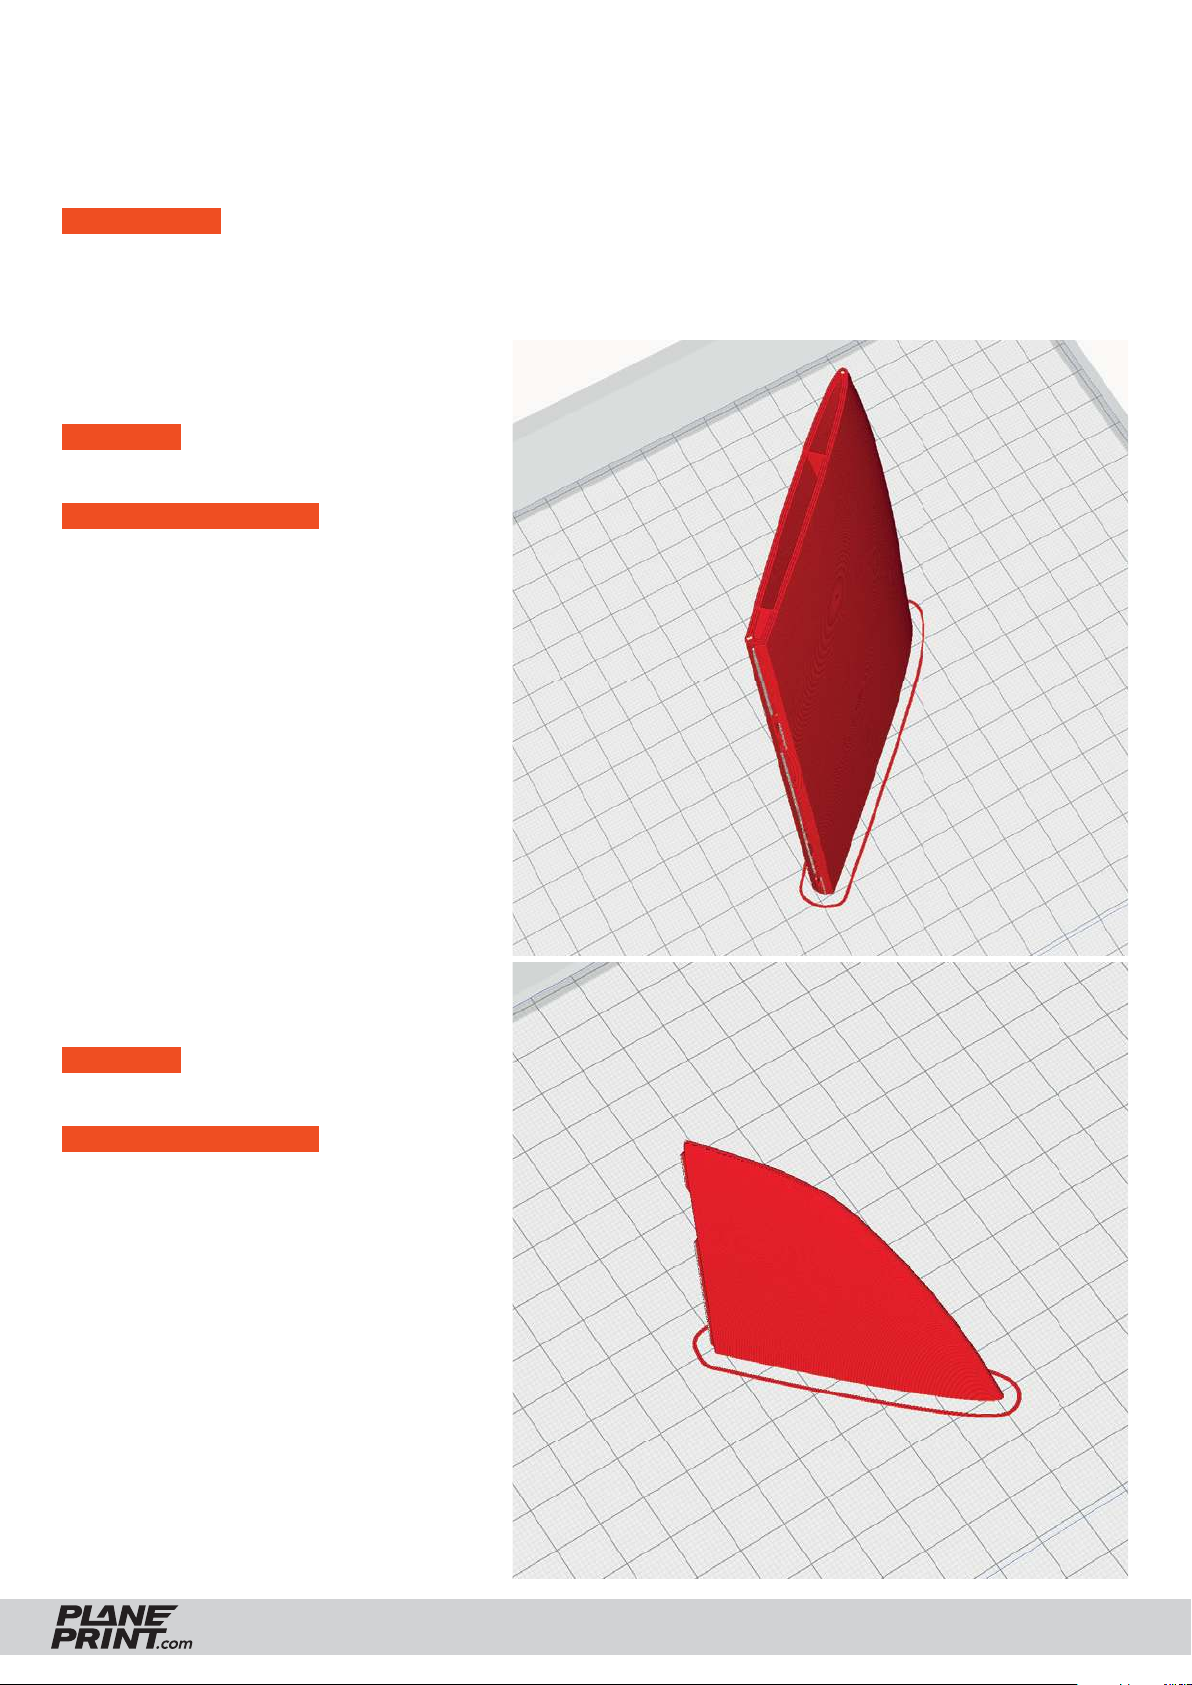
V-tail-left LW_profi le3_rise.stl
V-tail-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 20 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position left
right: • Z Seam Position right
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
V-tail2-left LW_profi le3_rise.stl
V-tail2-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 5 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
10
Page 11
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
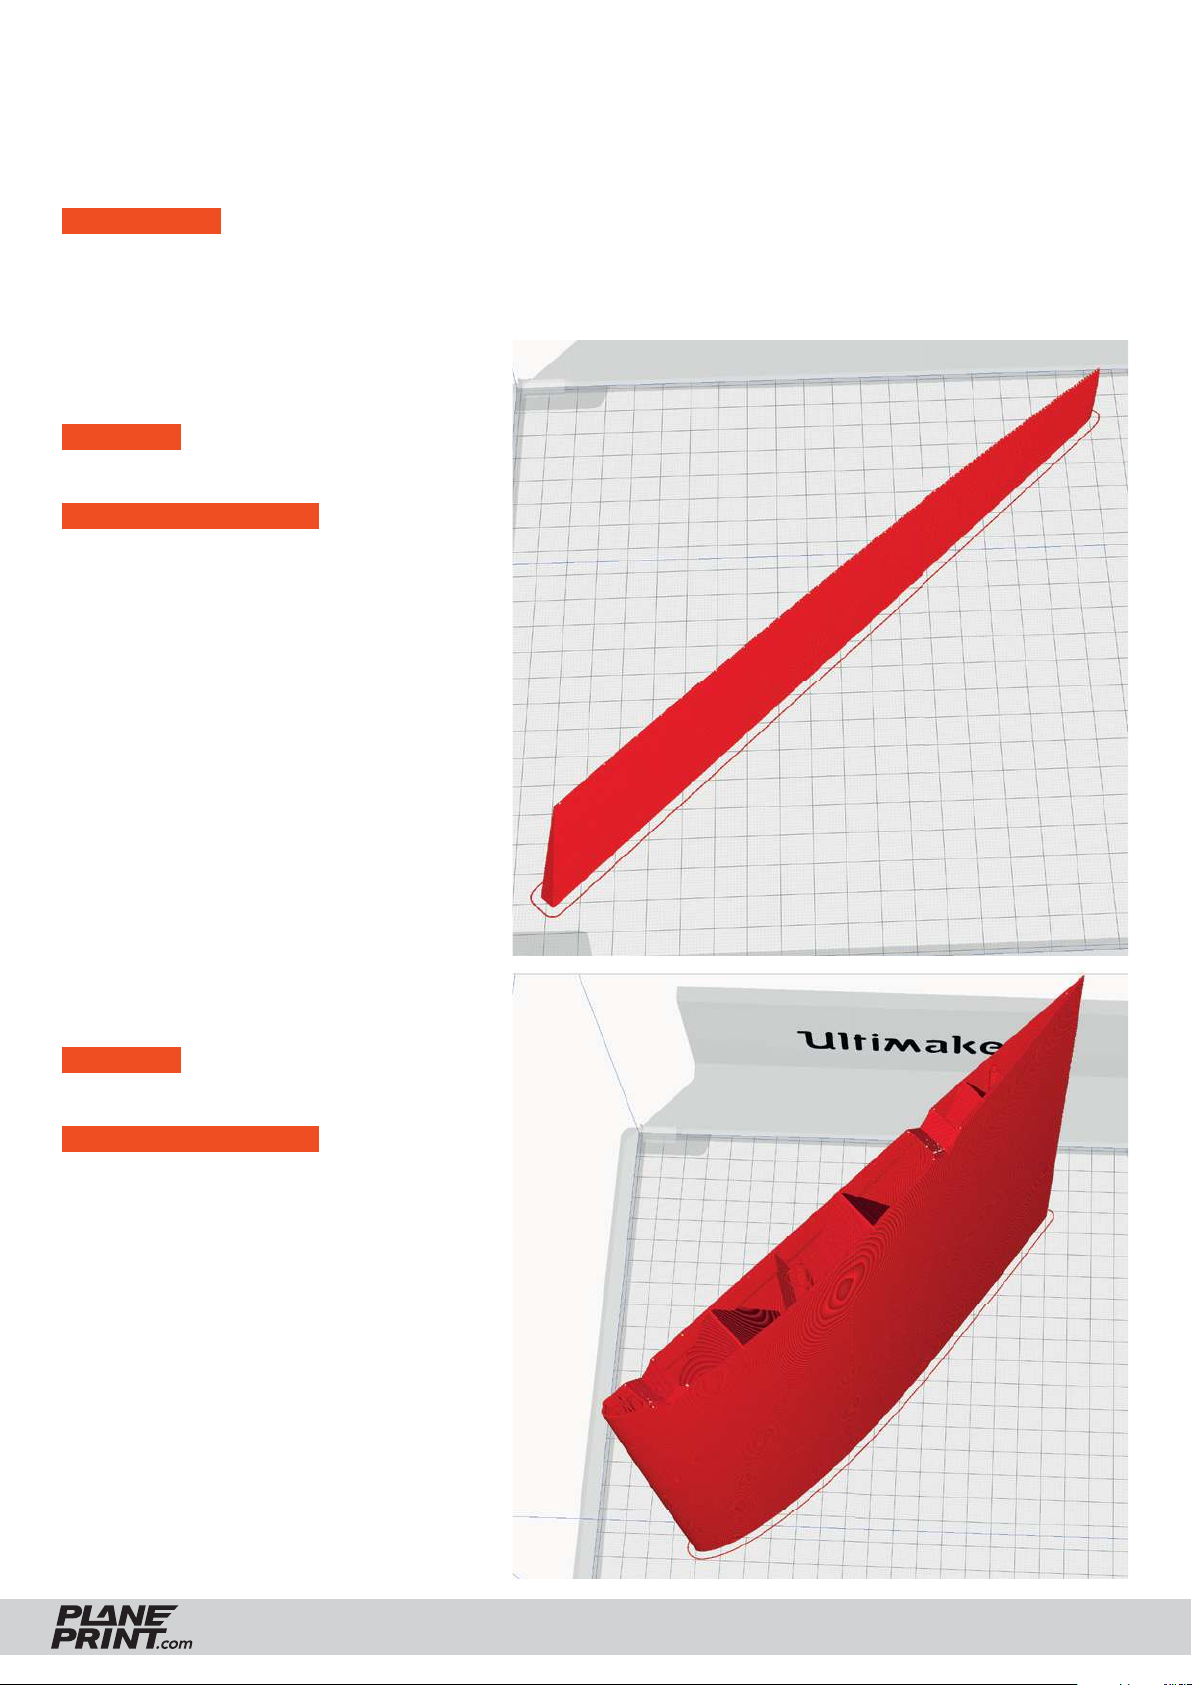
V-tail3-left LW_profi le3_rise.stl
V-tail3-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 11 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position right
right: • Z Seam Position left
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Wing1-left LW_profi le3_rise.stl
Wing1-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 70 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position right
right: • Z Seam Position left
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
11
Page 12
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
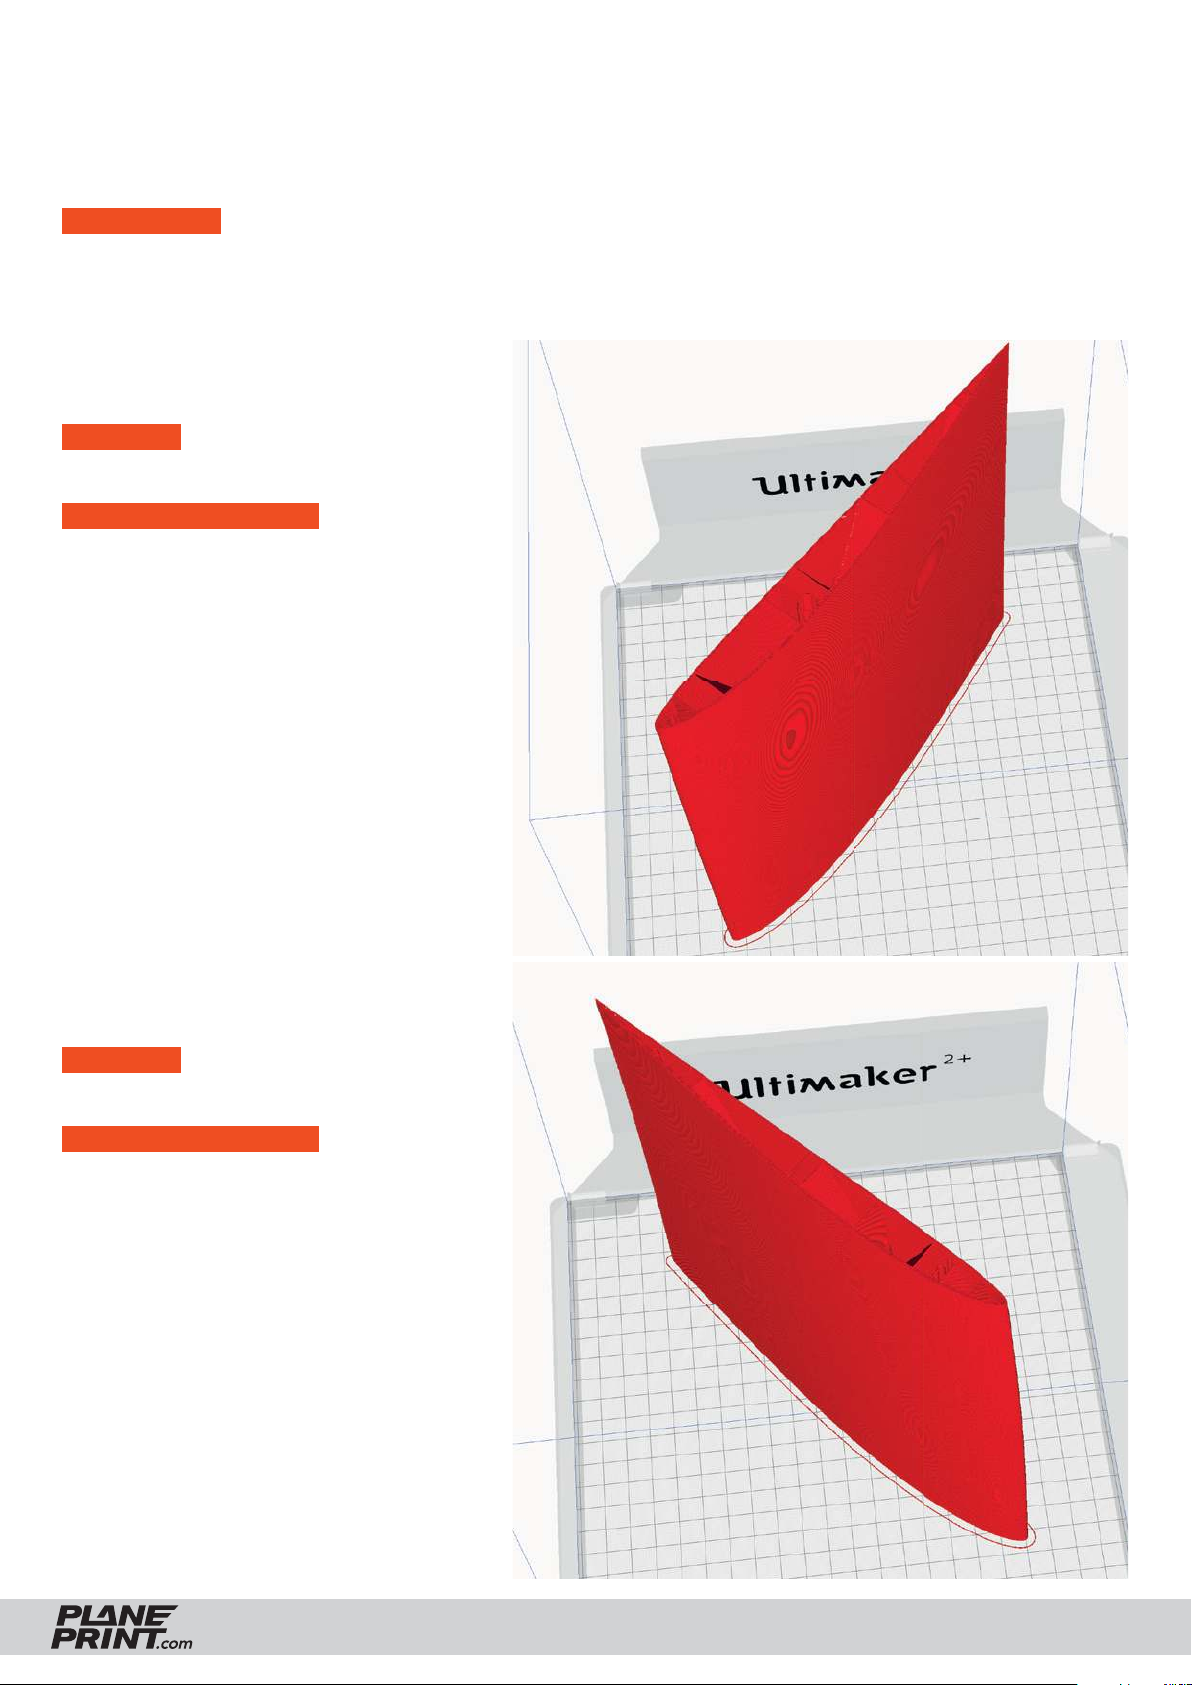
Wing2-left LW_profi le3_rise.stl
Wing2-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 68 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position right
right: • Z Seam Position left
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Wing3-left LW_profi le3_rise.stl
Wing3-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 63 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position left
right: • Z Seam Position right
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
12
Page 13
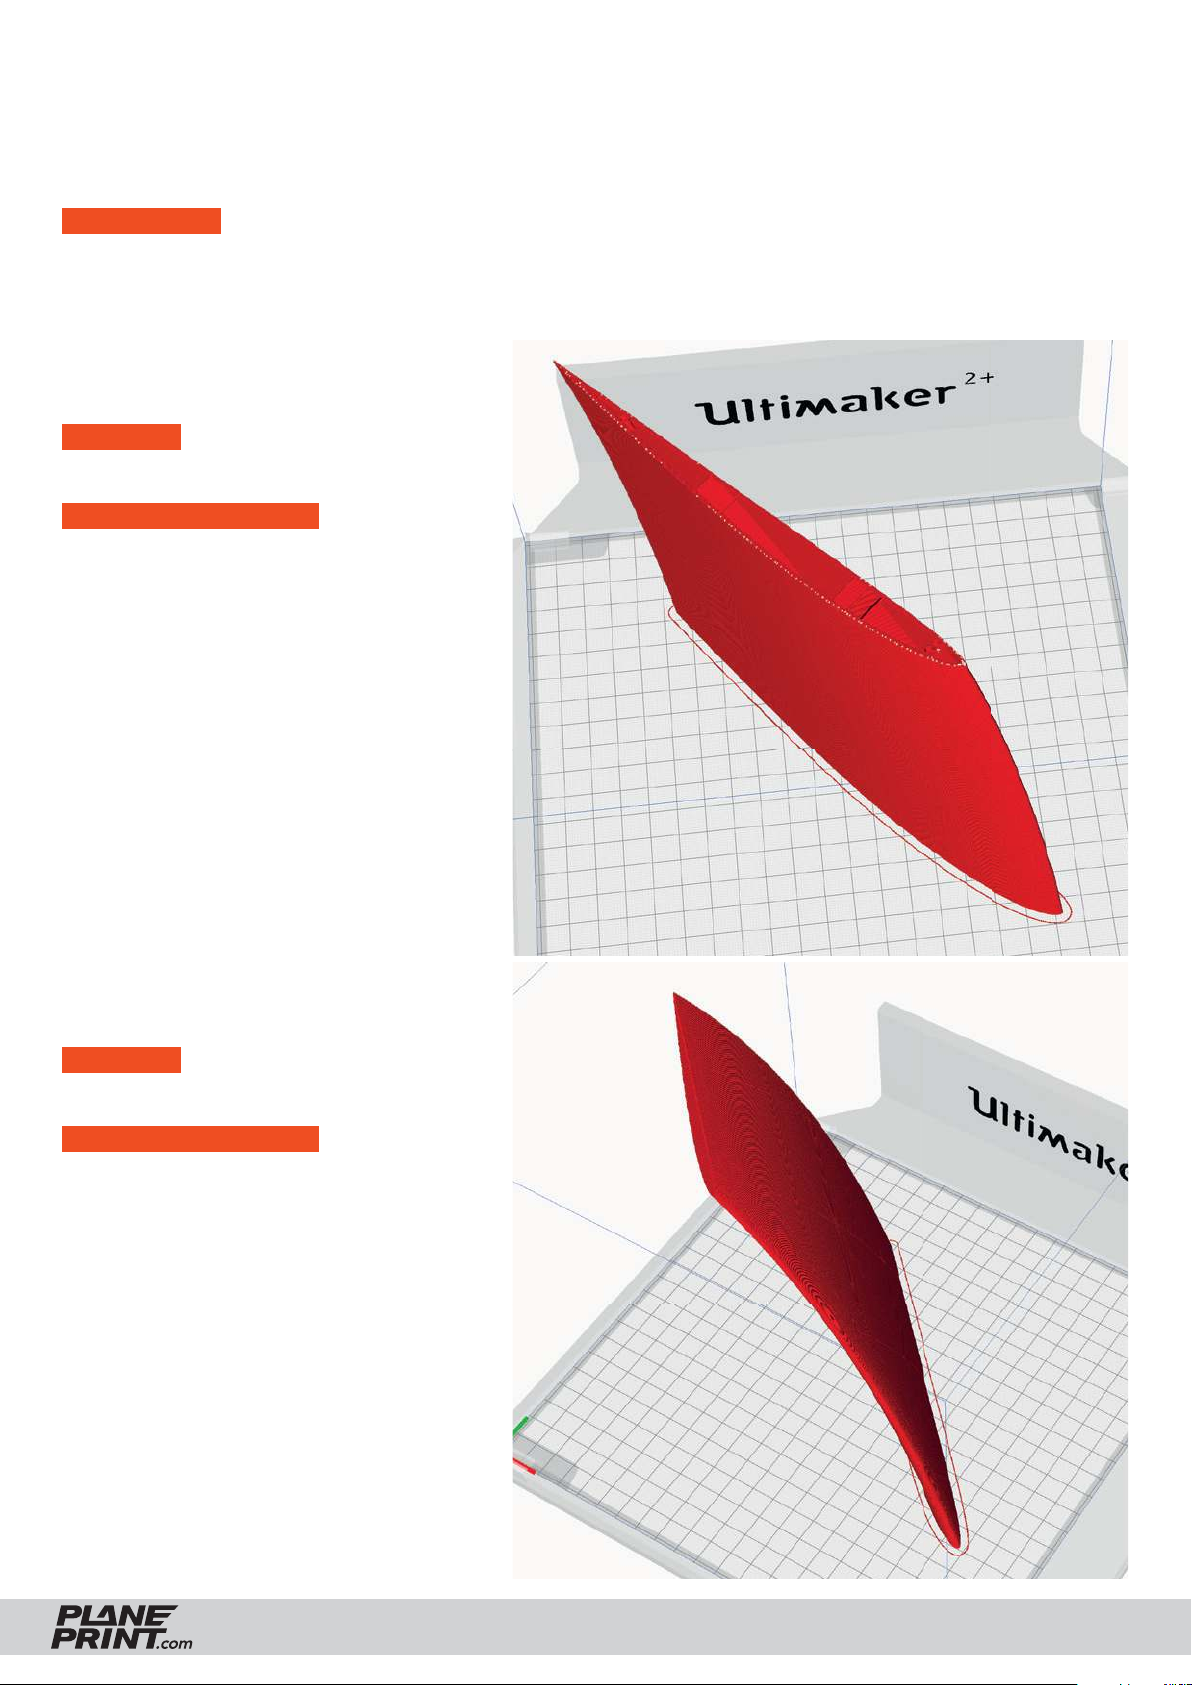
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
Wing4-left LW_profi le3_rise.stl
Wing4-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 52 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position left
right: • Z Seam Position right
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
Wing5-left LW_profi le3_rise.stl
Wing5-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 63 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
left: • Z Seam Position left
right: • Z Seam Position right
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
13
Page 14
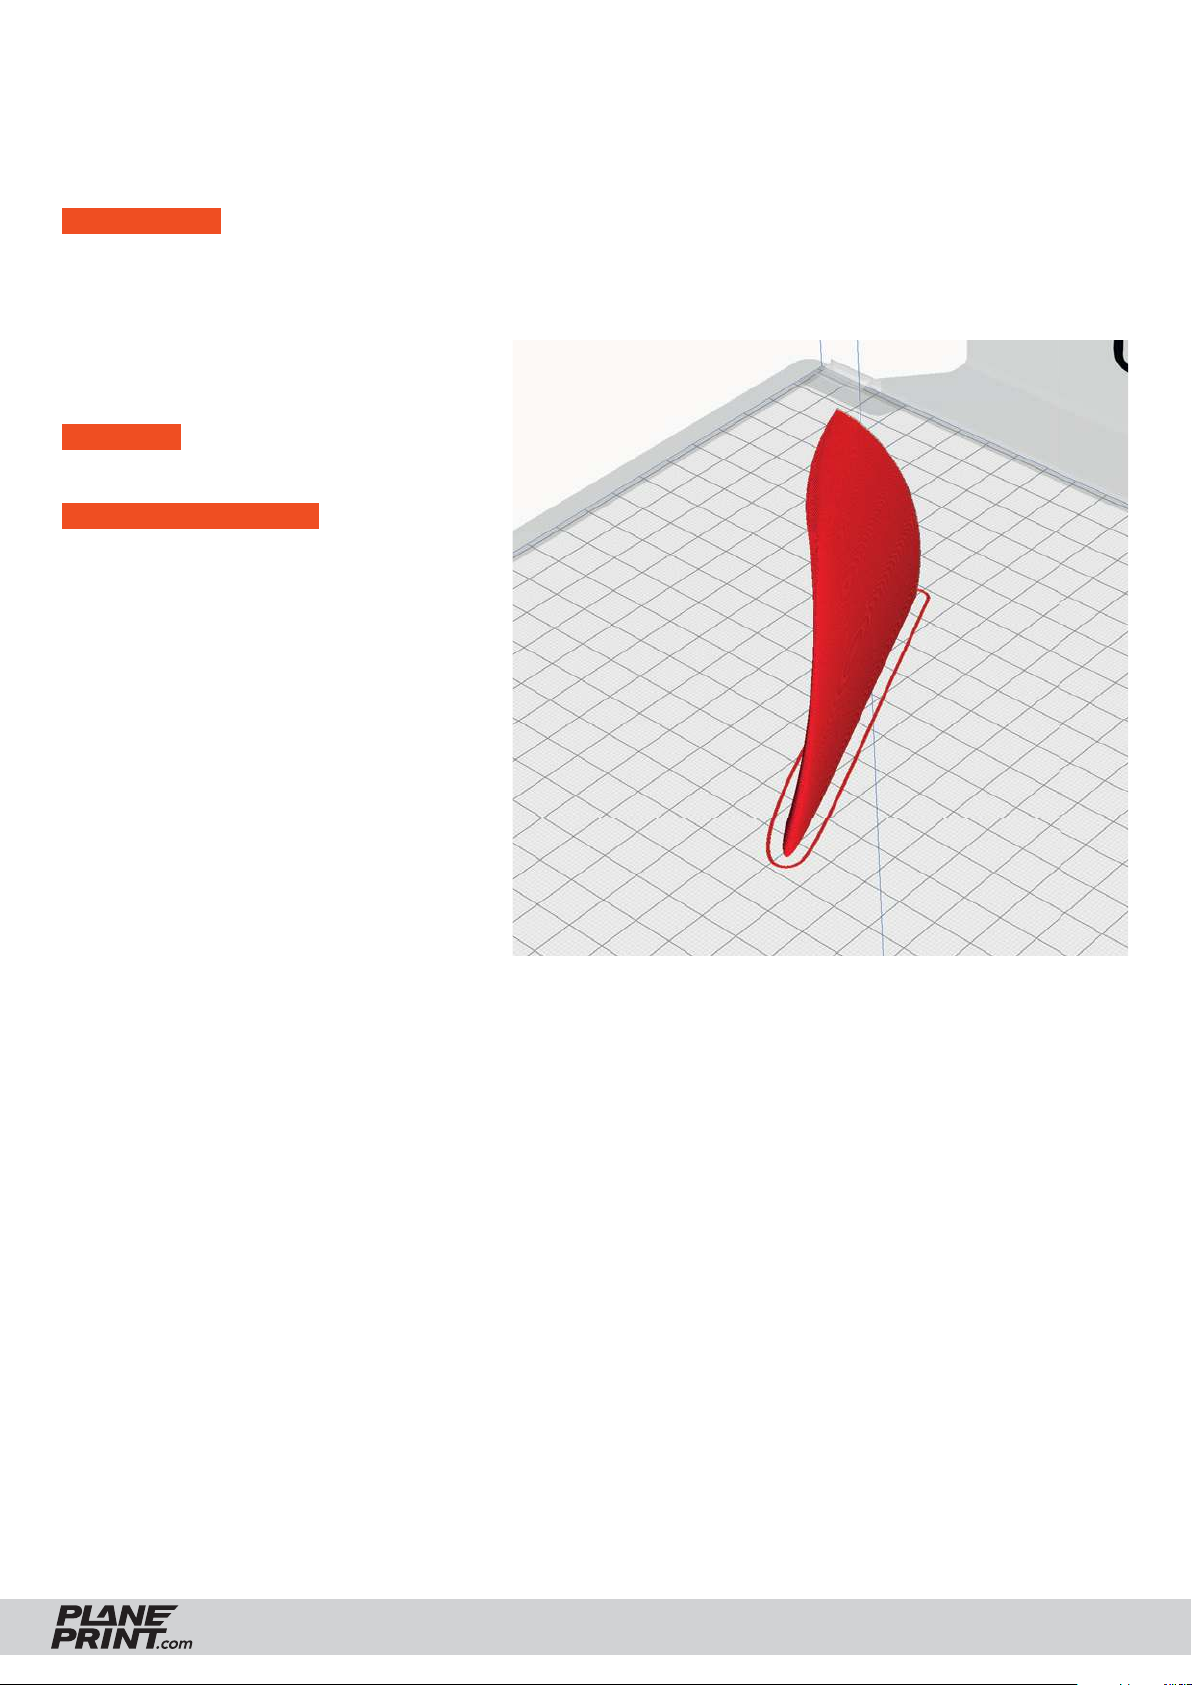
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profi le P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
Winglet-left LW_profi le3_rise.stl
Winglet-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 5 g*
*Display in Cura. The actual weight is then 60% of this.
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
Wing2 left: • Z Seam Position right
Wing2 right: • Z Seam Position left
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
14
Page 15
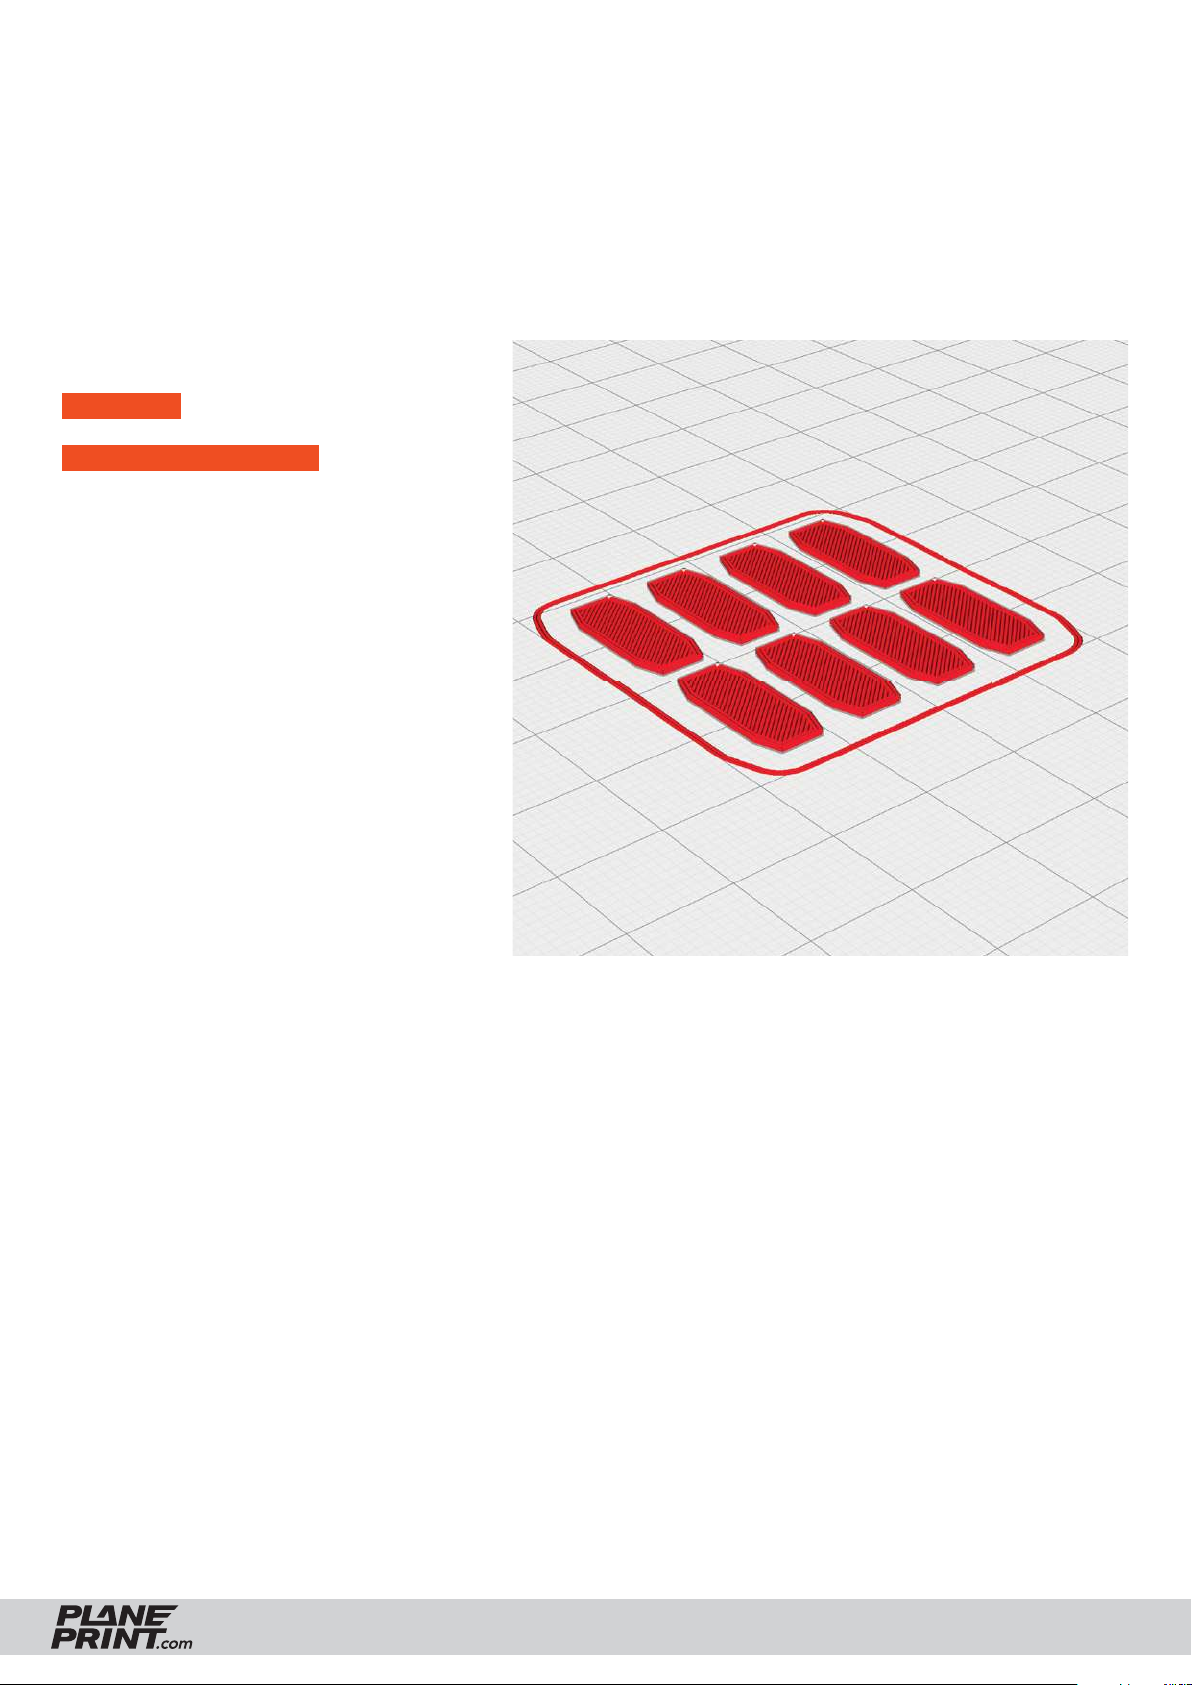
PROFILE P4_FLEX TPU A95
The following parts must be sliced with the PROFILE P4_FLEX.
Please note the additional settings for the individual parts!
N_Hinges_profi le4_rise.stl
MATERIAL TPU ~ A95, Weight: ~ 1 g
ADDITIONAL SETTINGS
None required
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
15
Page 16
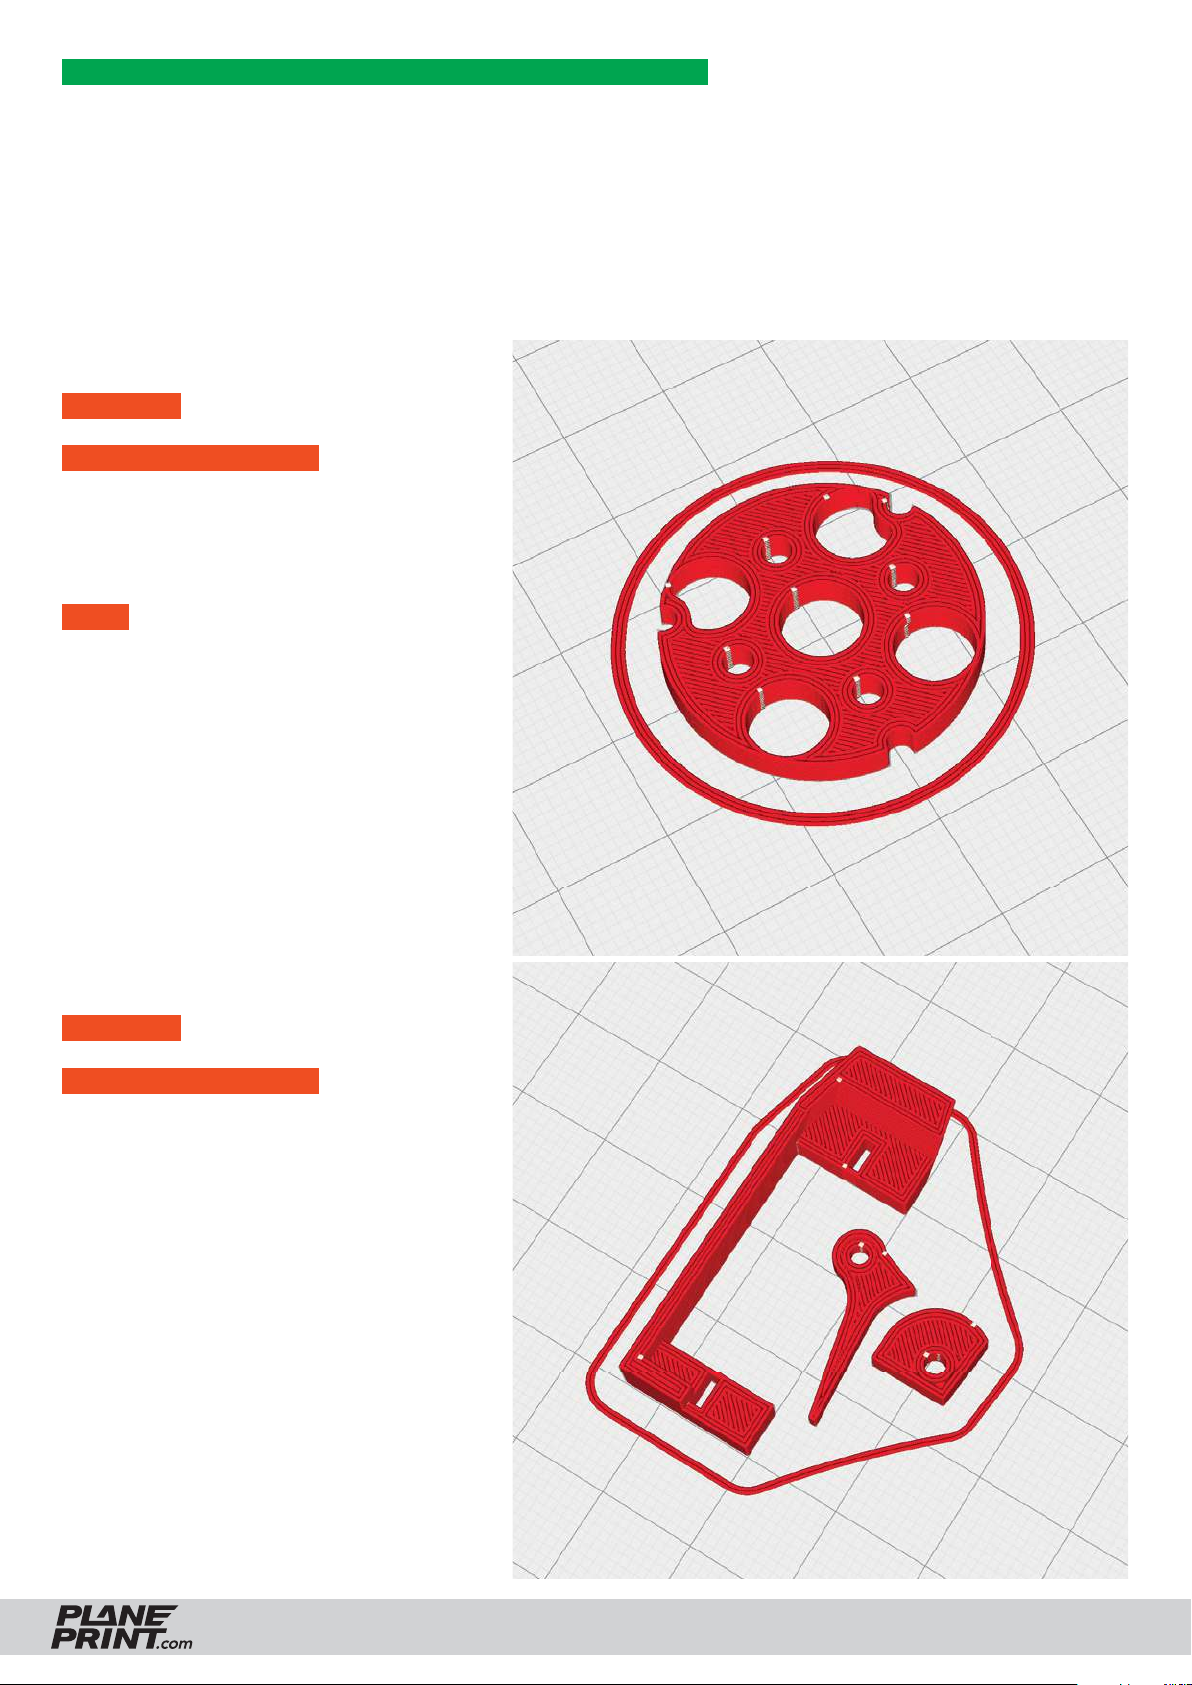
This parts are only required for the Motor/Spoiler upgrade Kit!
PROFILE P1_FULLBODY normal PLA
The following parts must be sliced with the PROFILE P1_FULLBODY.
Please note the additional settings for the individual parts!
Motormount 16_profi le1_rise.stl
MATERIAL PLA, ~ 2 g
ADDITIONAL SETTINGS
None required
INFO If your motor has other
hole spacing than 16 mm use the fi le
Motormount undrilled_profi le1.stl
Spoiler mount_profi le1_rise.stl
MATERIAL PLA, ~ 2 g
ADDITIONAL SETTINGS
None required
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
16
Page 17
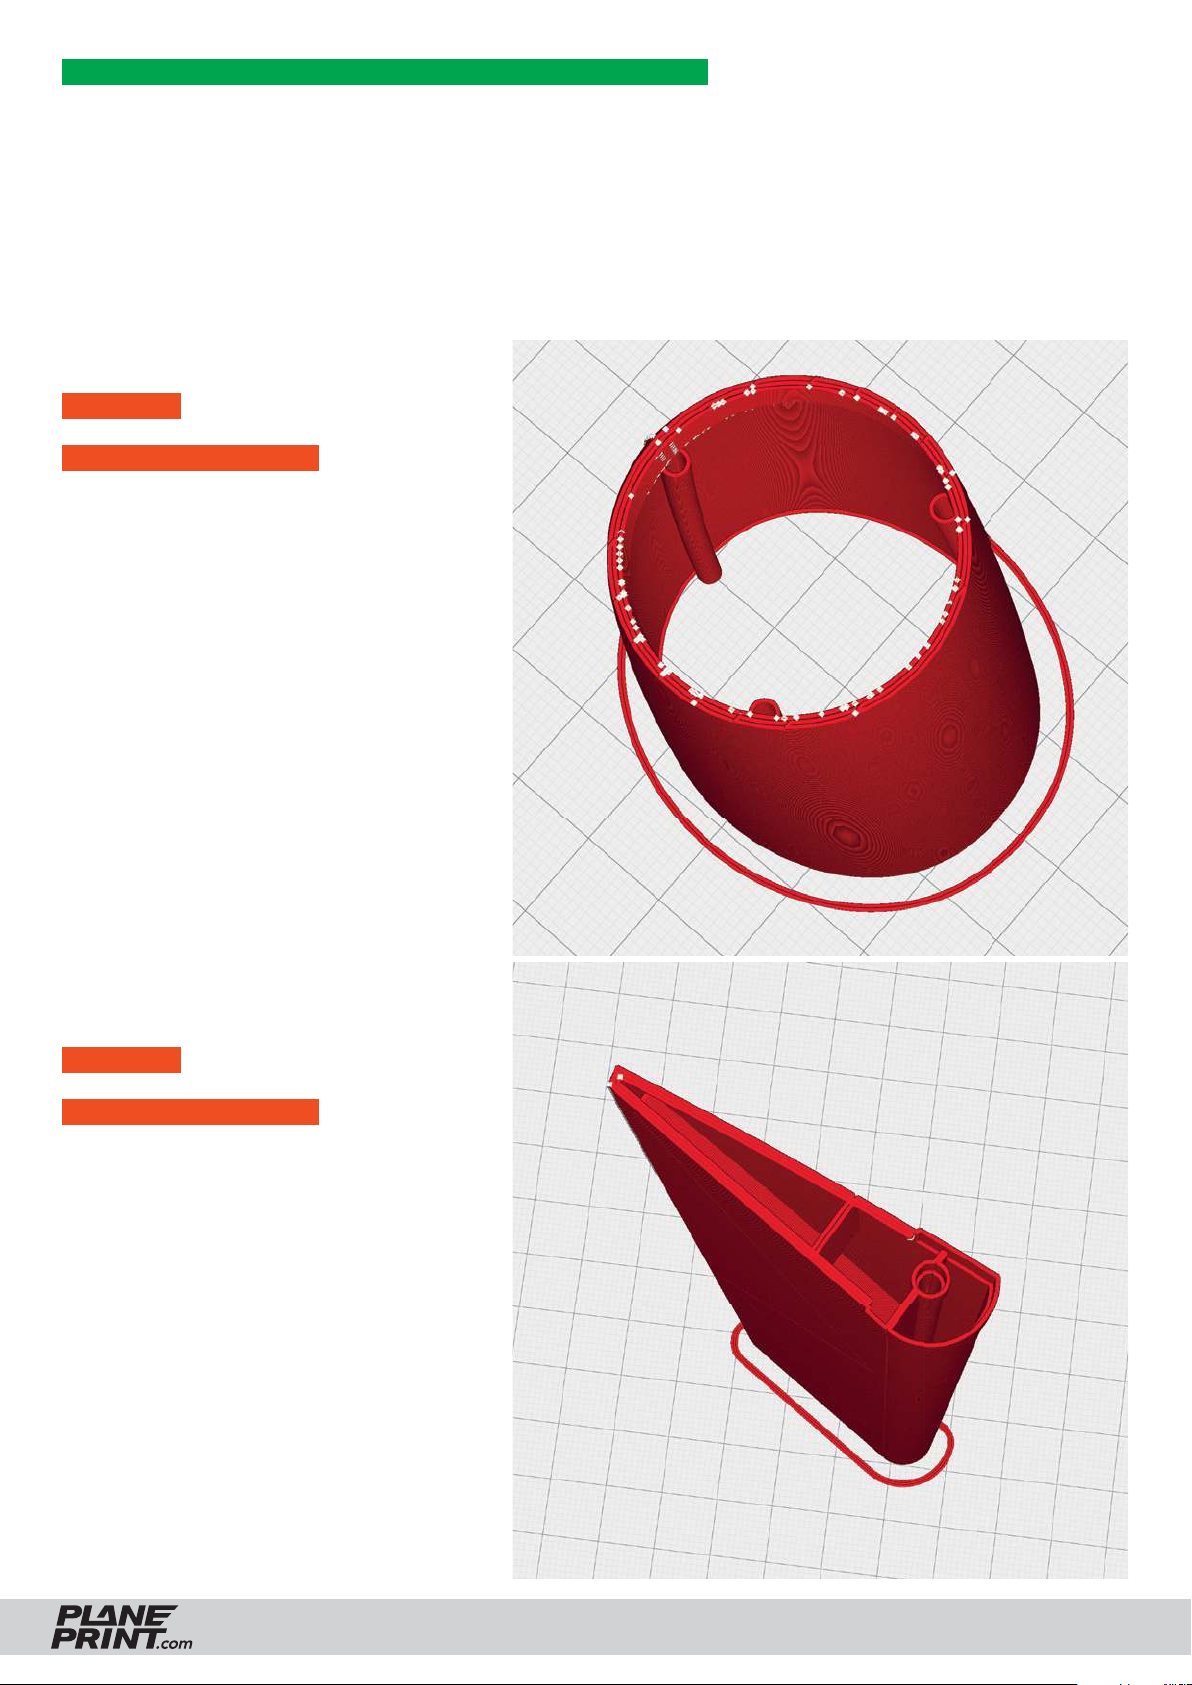
This parts are only required for the Motor/Spoiler upgrade Kit!
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
Nose motor LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 10 g*
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
*Display in Cura. The actual weight is then 60% of this.
Spoiler-left LW_profi le3_rise.stl
Spoiler-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 10 g*
ADDITIONAL SETTINGS
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
*Display in Cura. The actual weight is then 60% of this.
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
17
Page 18
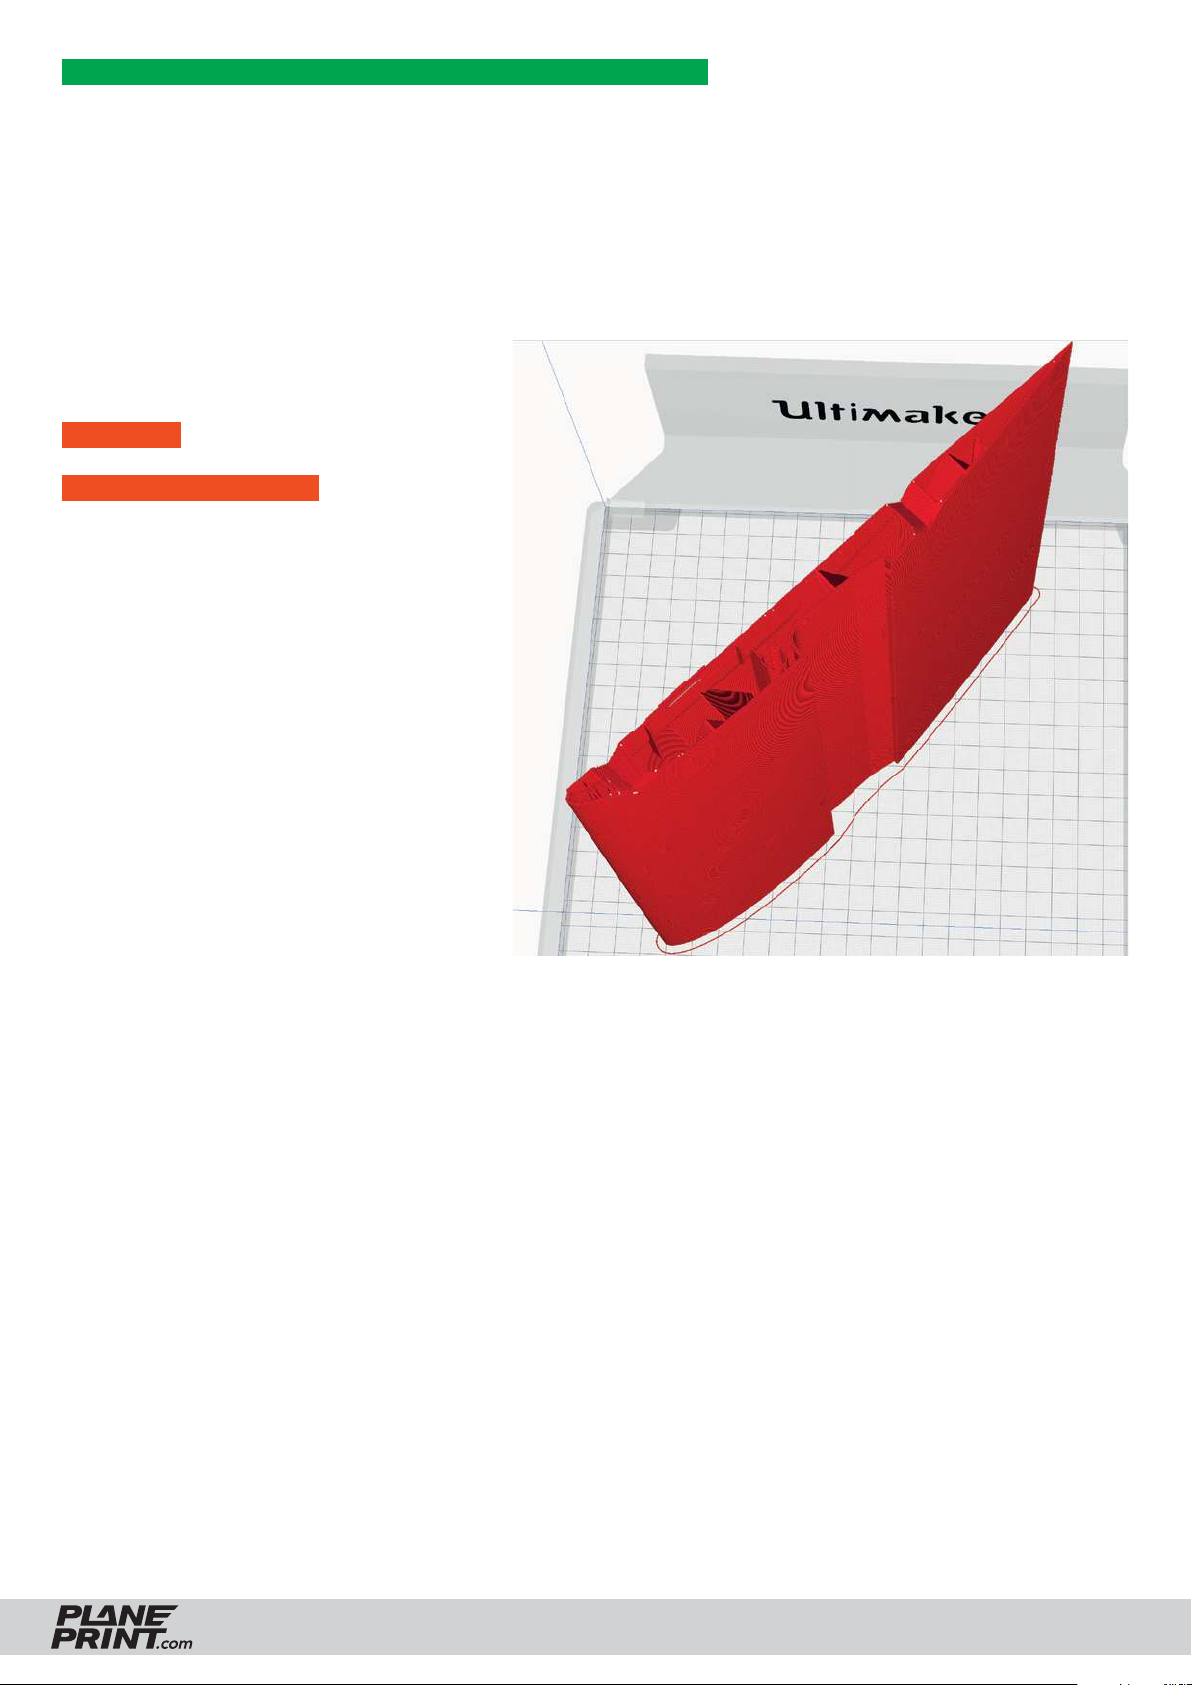
This parts are only required for the Motor/Spoiler upgrade Kit!
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
Wing1 spoiler-left LW_profi le3_rise.stl
Wing1 spoiler-right LW_profi le3_rise.stl
MATERIAL LW-PLA, ~ 69 g*
ADDITIONAL SETTINGS
left: • Z Seam Position right
right: • Z Seam Position left
- Setting Profi le3_Surface
- Flow 60 % or less
- Higher nozzle temperature
The optimal weight and suffi cient strength is achieved
with 60 % fl ow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% fl ow).
*Display in Cura. The actual weight is then 60% of this.
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
18
Page 19
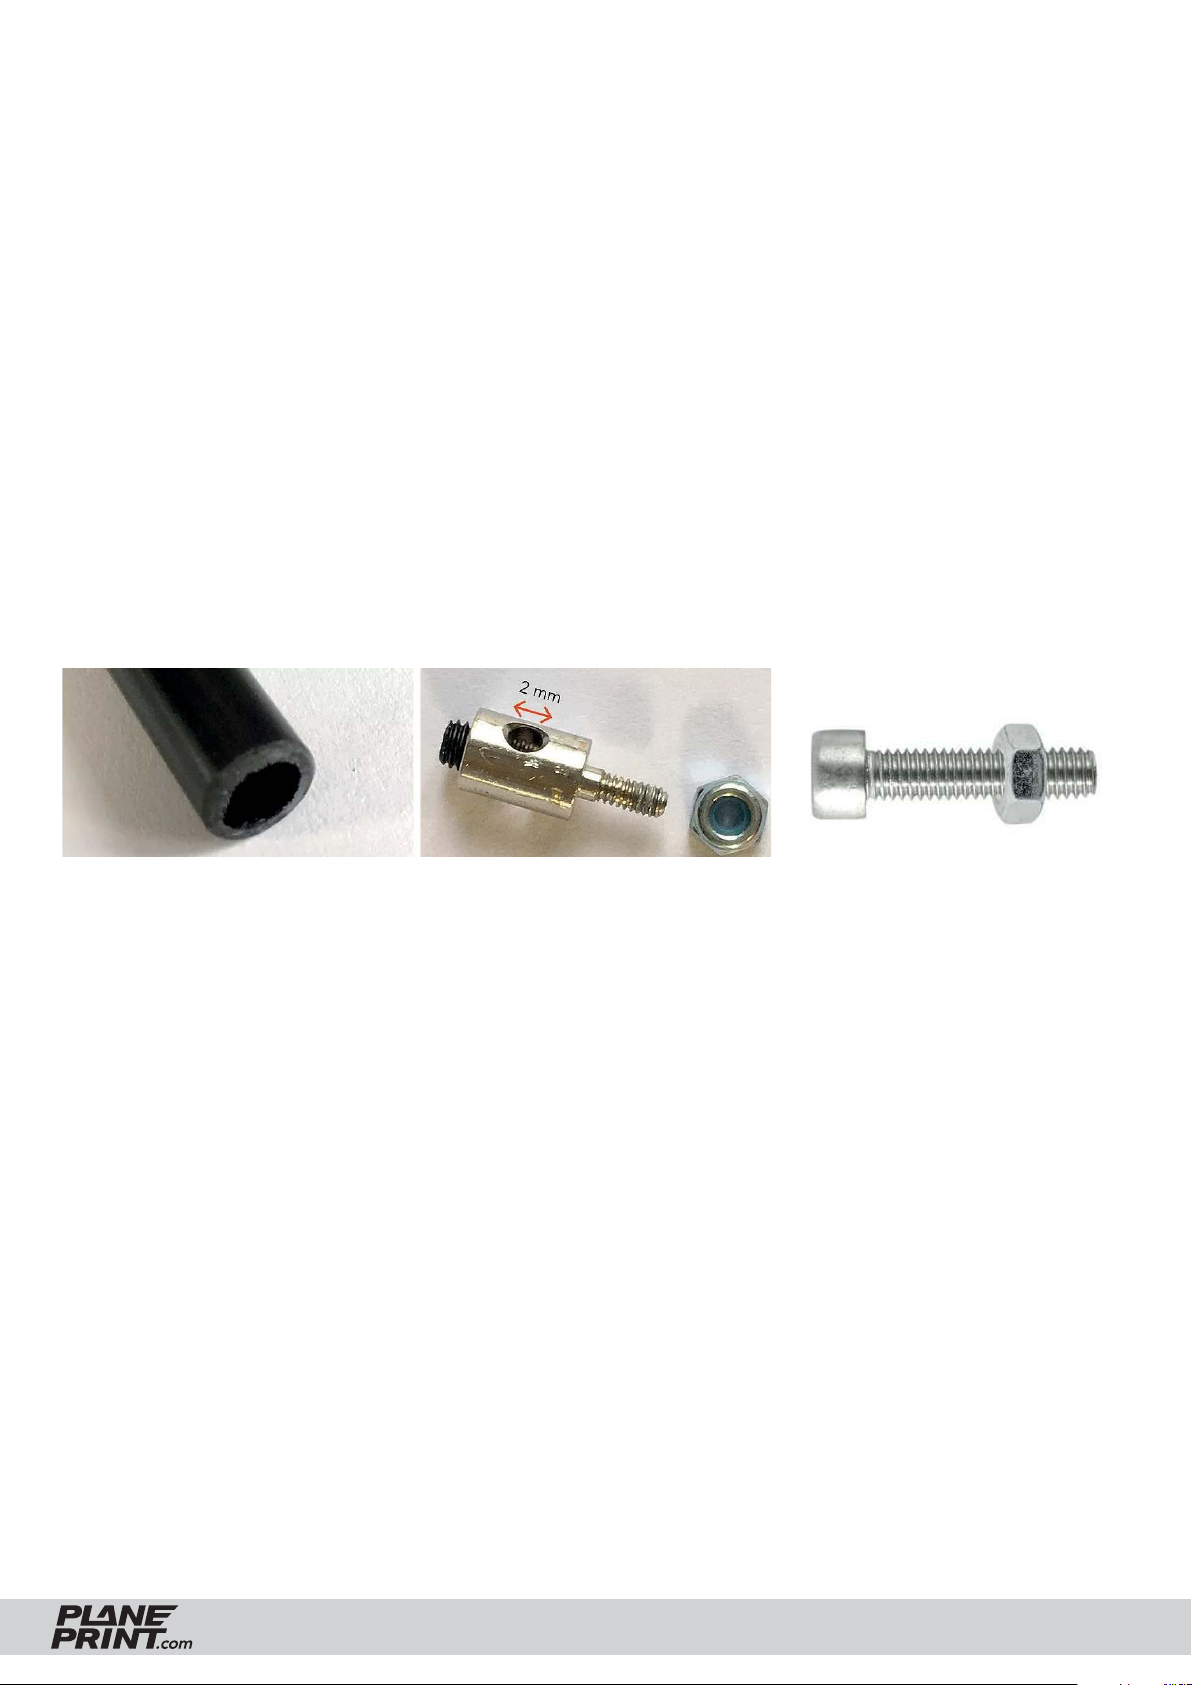
REQUIRED ACCESSOIRES
Filament
• normal PLA about 50 grams
• LW-PLA about 500 grams
We strongly recommend using white (natural) LW-PLA, which heats up much less in direct sunlight.
• TPU (A95) about 10 grams
(ABSOLUTELY NECESSARY)
Materials
• Socket Head Screw Ø3mm*22mm with nut, 2 pieces
• CA super glue (liquid and liquid medium)
• CA activator
• Carbon tube Ø6*1000mm (inside Ø4mm), 1 piece
• Carbon rod Ø1.2mm*1000, 6 pieces (better plus one as reserve)
• Steel wire Ø1mm, short piece for the servo linkages
• Rod connection, 2 pieces
Tools
• Cutter knife
• small Philips screwdriver
• needle-nose pliers
Rod connectionCarbon tube Socket Head Screw with nut
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
19
Page 20
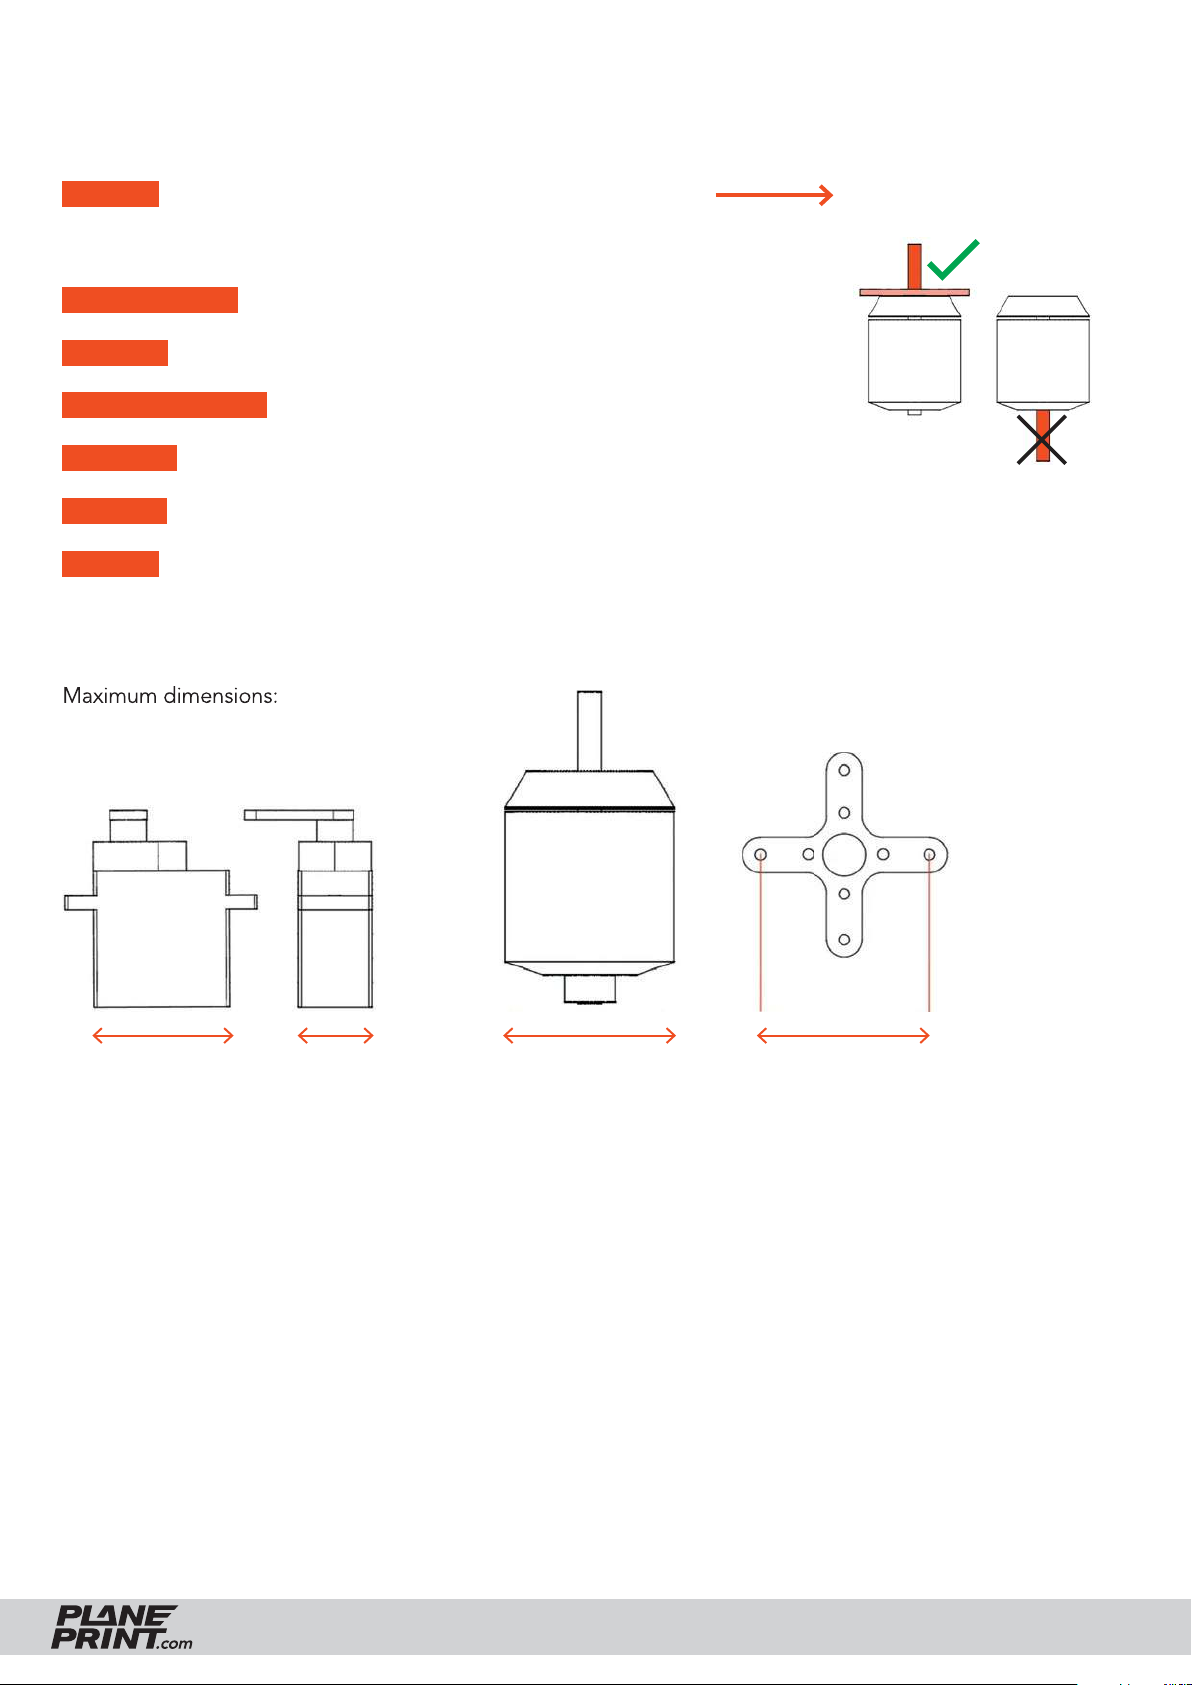
RC Components
ENGINE • Topmodel XPower XC2212/18 (our recommendation)
• or Roxxy C22-20-20 1330kv
or comparable motors
FOLDING PROP 7,5x4
SPINNER Ø 30 mm
BEC-CONTROLLER min. 15 A (must fi t the engine!)
RECEIVER Glider: 3 Channel, Motorized version: 5 Channel
BATTERY 3S Lipo, about 600-1000 MaH
SERVOS Hitec HS-5055MG or (or similar in the same size), 2 or 3 pieces
Maximum dimensions:
Pay attention to the position
of the motor shaft
RISE
Ø max. 22 mm max. 23 mm max. 13 mm 16 mm
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
20
Page 21
Page 22
ASSEMBLING MANUAL
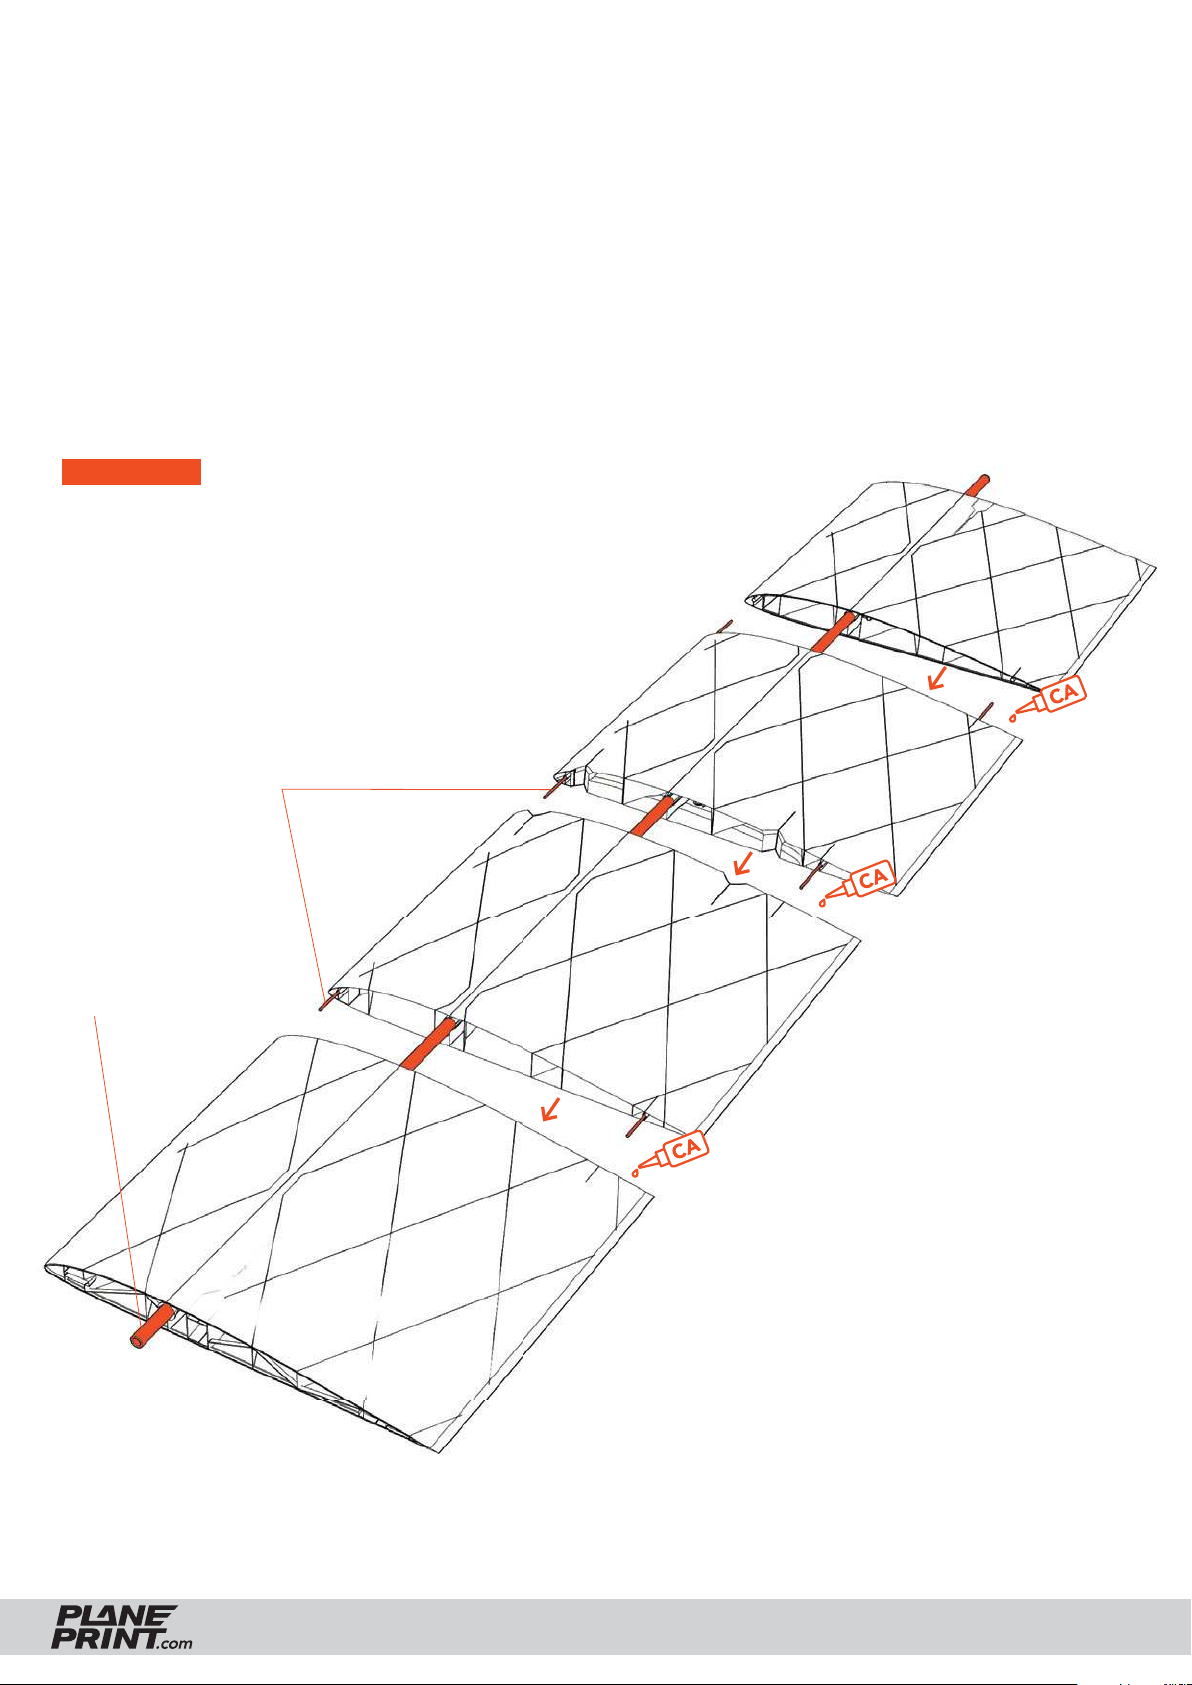
Wings assembly – Middle part
Cut six short pieces of carbon rod with the knife and use them as
dowel pins to accurately glue the wing parts together. The bonding
surfaces should be roughened with sandpaper beforehand to
achieve a perfect bond.
IMPORTANT The carbon tube must NOT be glued!
Wing2-right LW_profi le3_rise.stl
Carbon rods Ø1,2*30mm
Carbon tube Ø6*1000mm
Wing1-right LW_profi le3_rise.stl
medium l.
medium l.
Wing1-left LW_profi le3_rise.stl
medium l.
RISE
Wing2-left LW_profi le3_rise.stl
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
22
Page 23
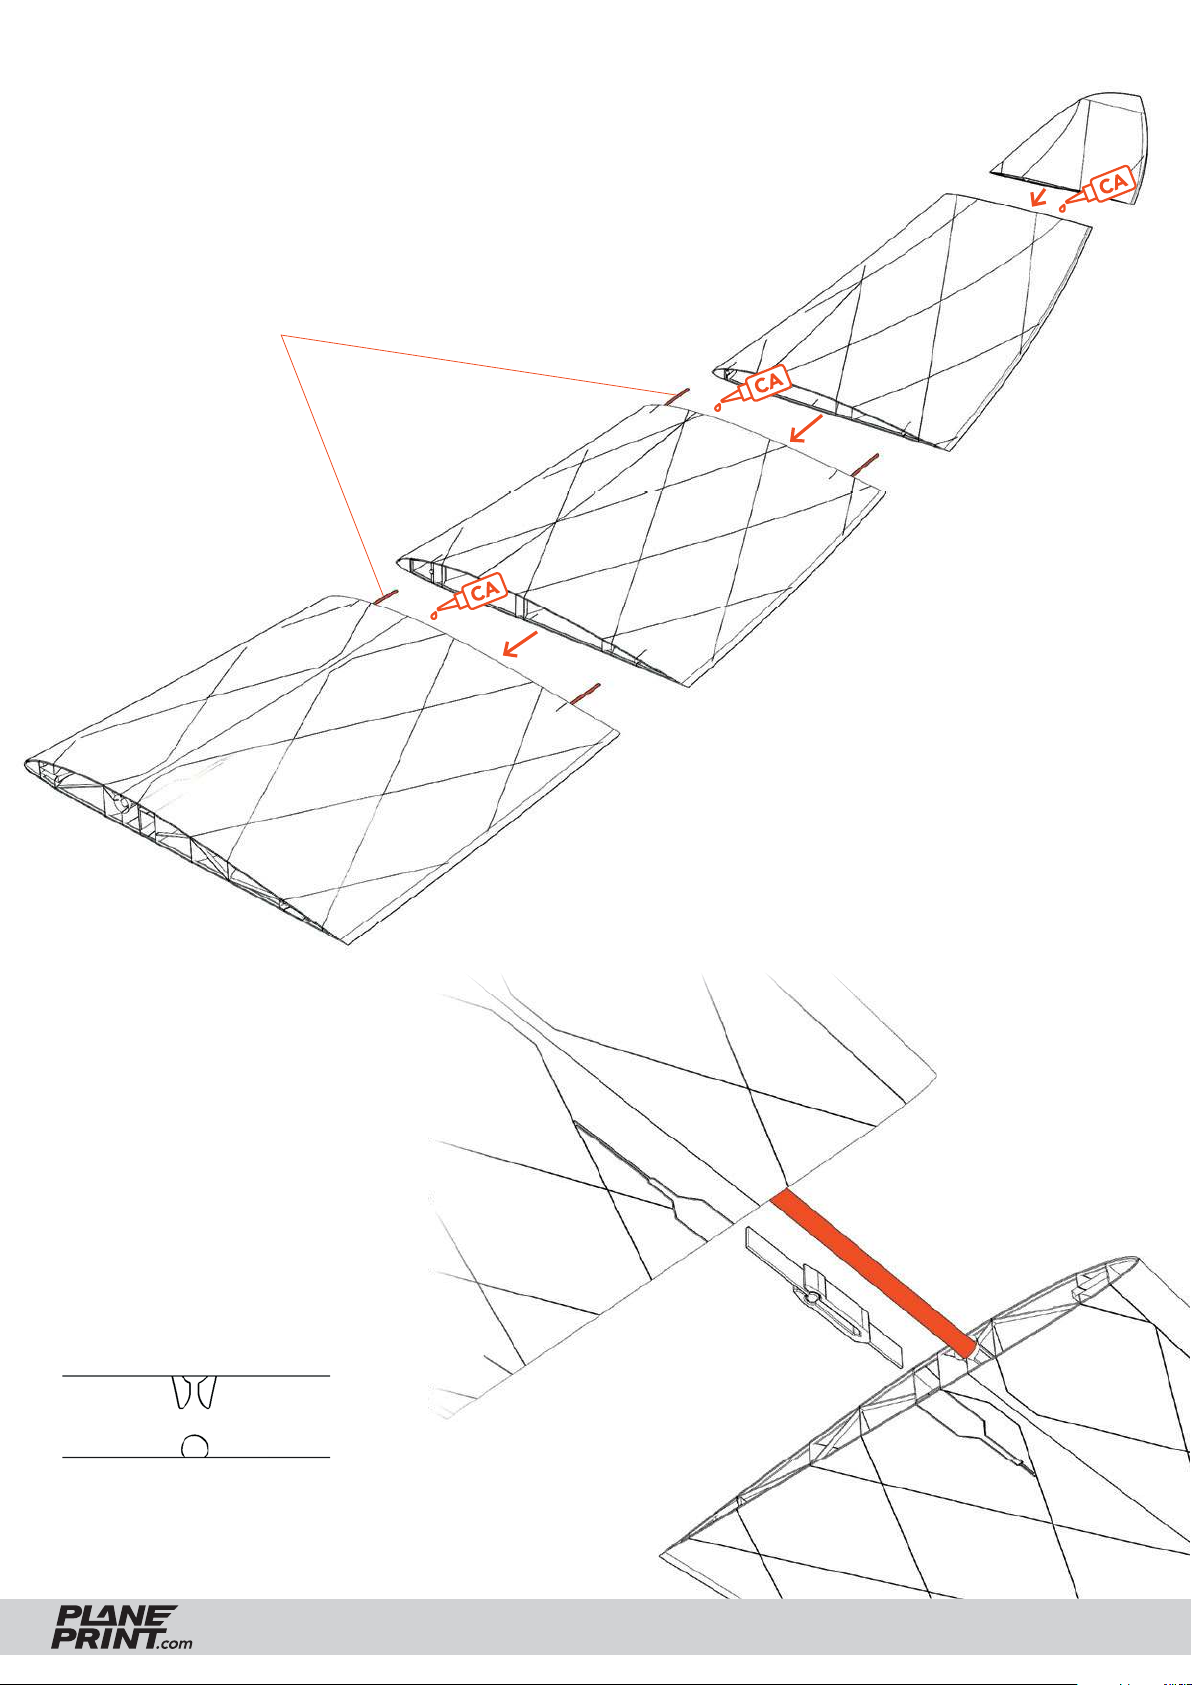
Wings assembly – Side parts
Glue the outer wing parts in the same way.
Wing5-right LW_profi le3_rise.stl
Carbon rods Ø1,2*30mm
Wing4-right LW_profi le3_rise.stl
Wingtip-right LW_profi le3_rise.stl
medium l.
medium l.
Wing3-right LW_profi le3_rise.stl
Wing Snap Lock
This mechanism allows easy
assembly of the wing parts without
tools. Insert the parts into the slots
provided as far as they will go and
check that they engage exactly
when the wing parts are assembled
before gluing.
medium l.
Wing3 LW_profi le3_rise.stl
Wing2 LW_profi le3_rise.stl
RISE
Snap lock_profi le1_rise.stl
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
23
Page 24
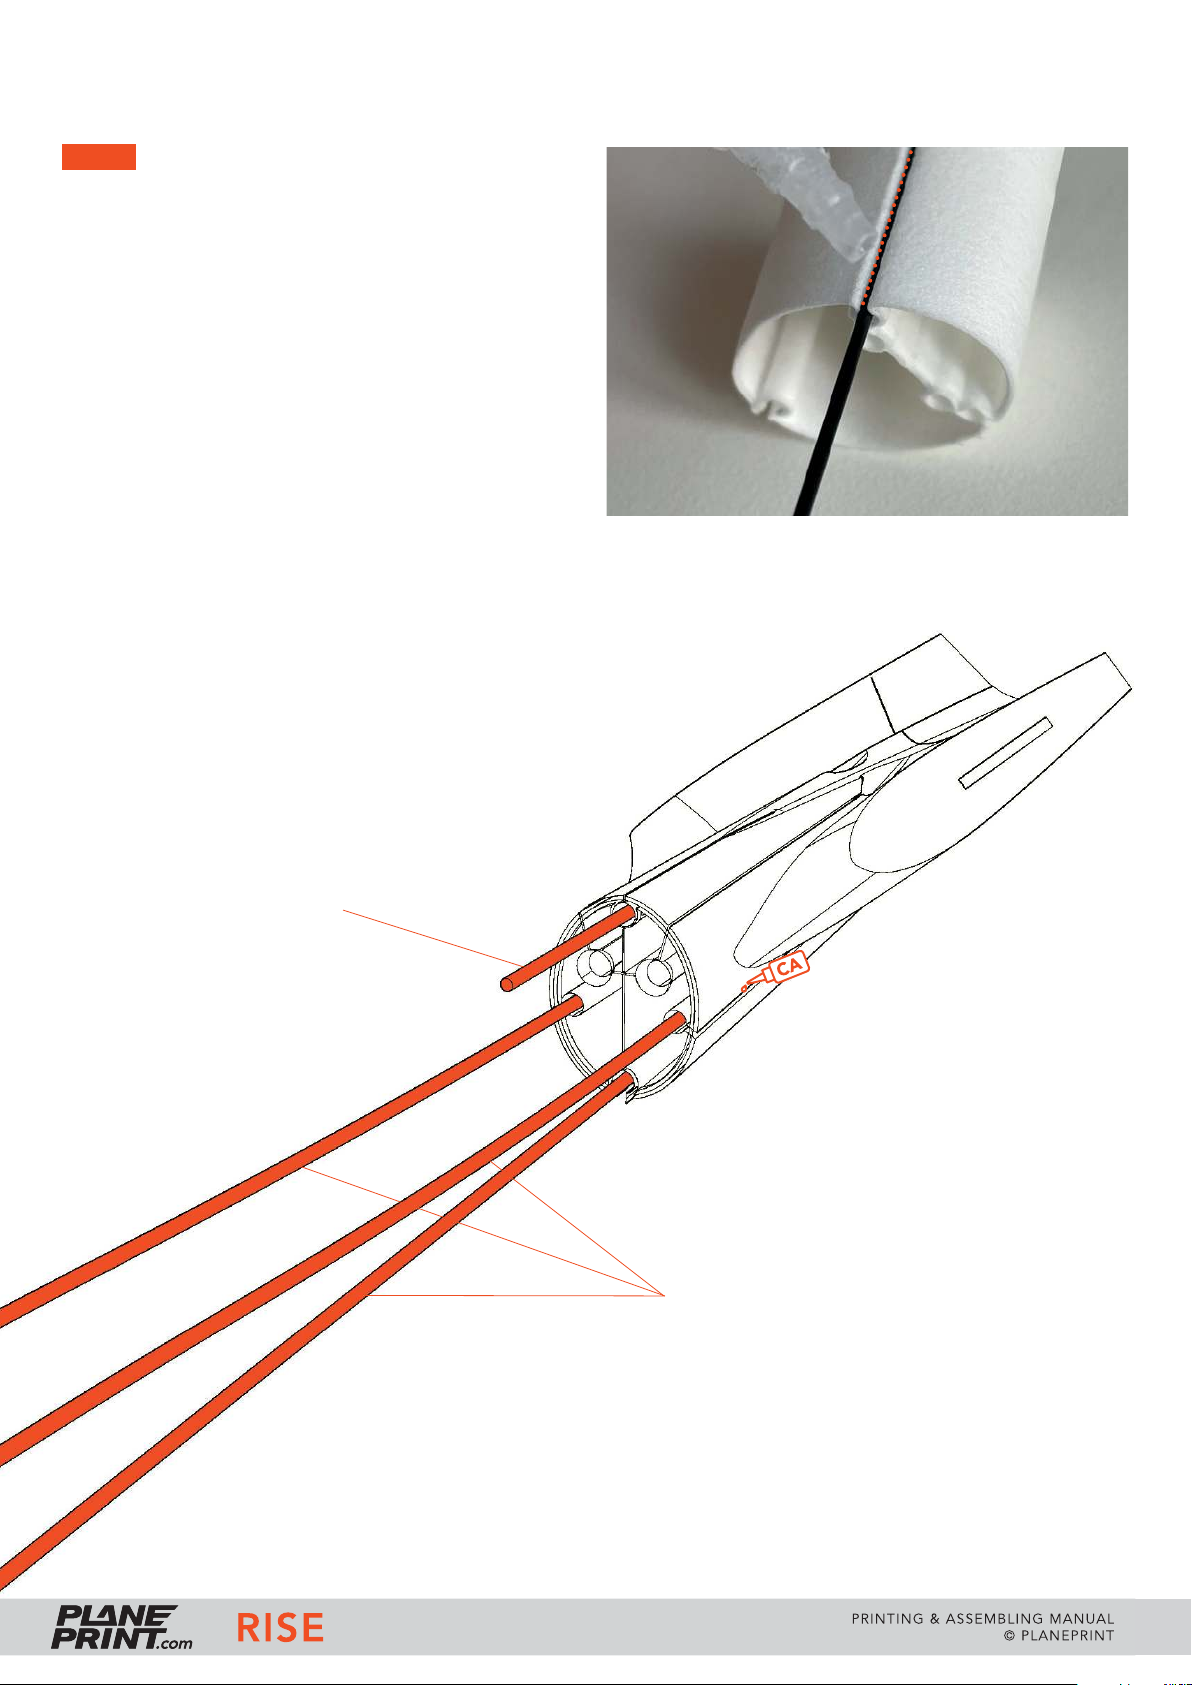
Fuselage assembly
NOTE To build the thin fuselage suffi ciently stable,
it is very important that the carbon rods are glued to
the LW-PLA over the entire length.
Therefore, there are open gaps along the carbon
rods on the outer surface of the fuselage. Pour thin
CA glue into these gaps along the entire length to
create a complete bond between the LW-PLA and
the carbon rod.
Start with the fuselage 6 part and glue the carbon
rods well with thin CA glue. The three long rods must
reach all the way to the end!
Carbon rod Ø1,2*55mm
Fuselage6 LW_profi le3_rise.stl
thin
RISE
Carbon rods Ø1,2*1000mm
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
24
Page 25
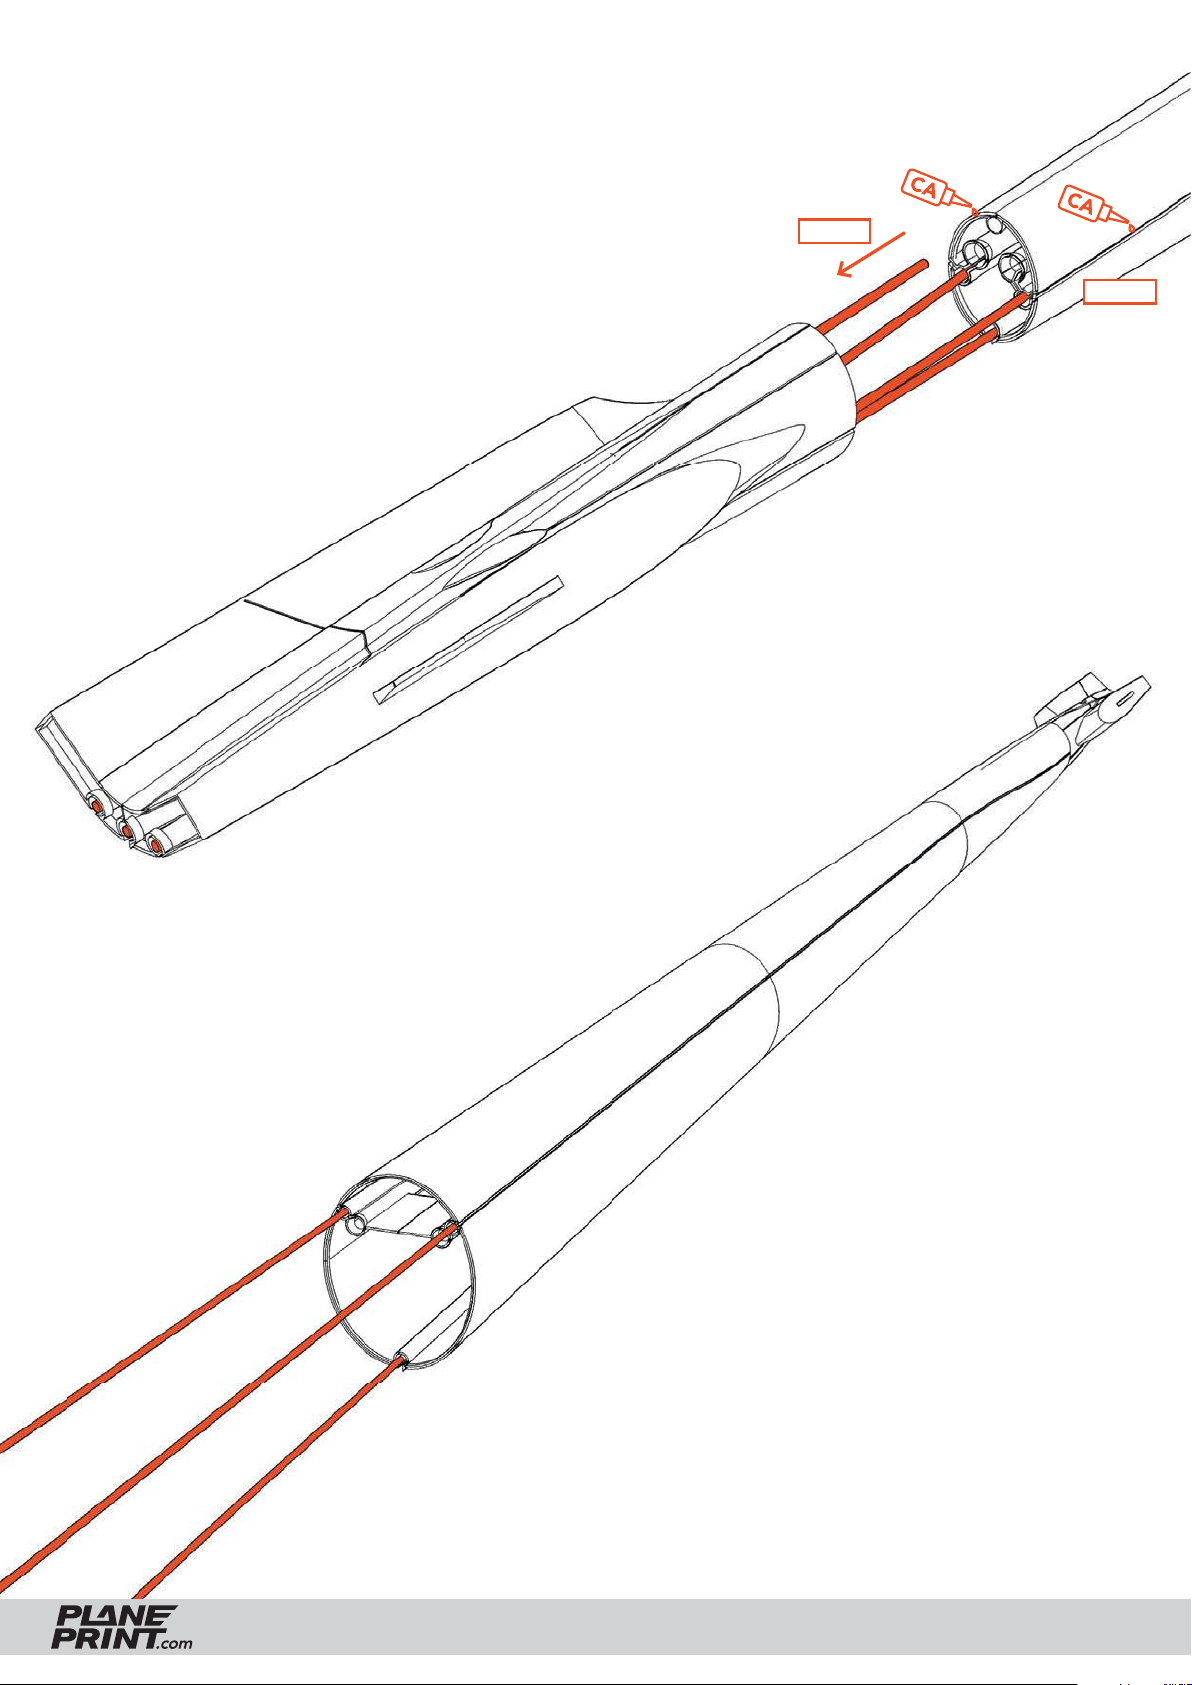
Fuselage assembly
Then place fuselage 5 on the carbon rods and glue
only the two fuselage parts with medium CA glue.
Do not forget to roughen all gluing surfaces with
sandpaper!
Then check that fuselage 5 is aligned straight and run
thin CA glue into the gaps along the outer surface
to bond the carbon rods to the fuselage along their
entire length.
Fuselage6 LW_profi le3_rise.stl
STEP 1
Fuselage5 LW_profi le3_rise.stl
medium l.
thin
STEP 2
Fuselage6 LW_profi le3_rise.stl
Repeat with the fuselage parts 4 and 3 ...
Fuselage5 LW_profi le3_rise.stl
Fuselage4 LW_profi le3_rise.stl
Fuselage3 LW_profi le3_rise.stl
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
25
Page 26
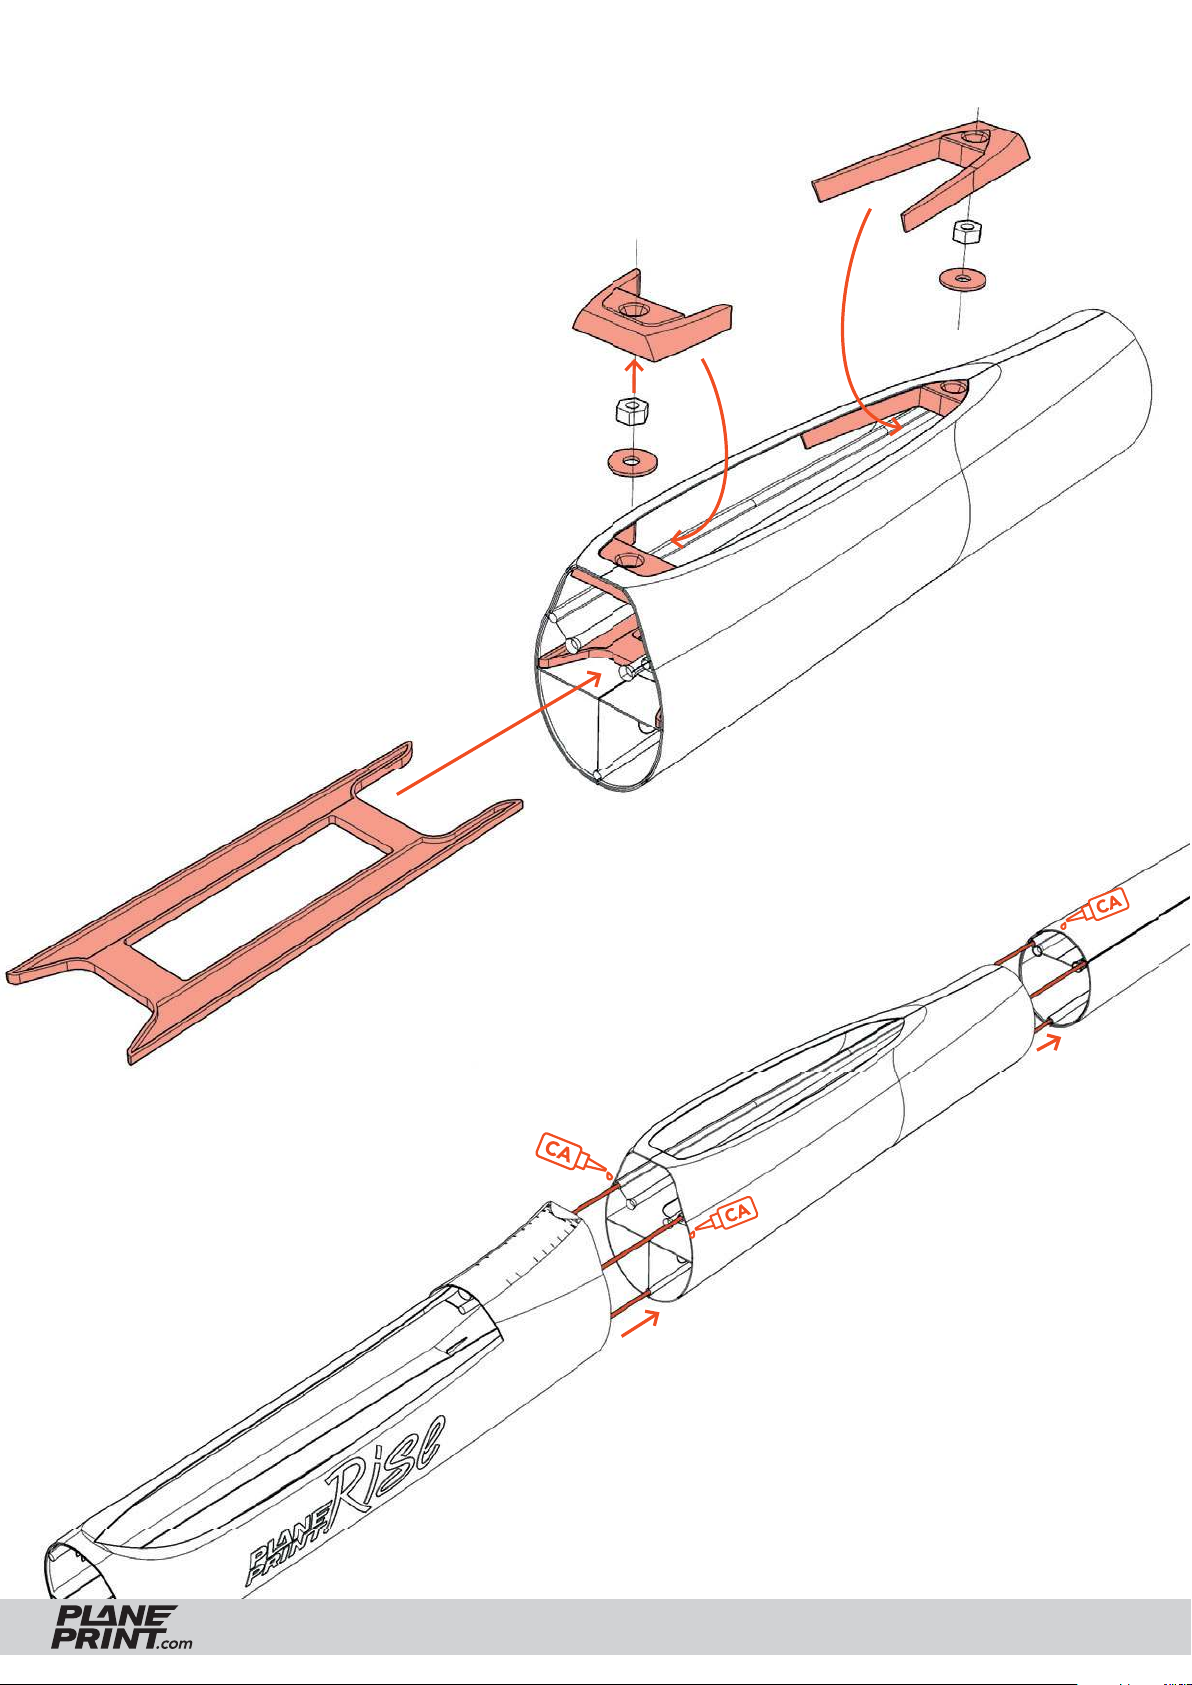
Fuselage assembly
Before gluing fuselage 2 to the fuselage,
some PLA parts have to be mounted: Glue
the Ø3mm nuts into the wingmount parts
and then into the fuselage 2. Push the
spacer from the front into the fuselage 2
and glue it well.
Wingmount_profi le2_rise.stl
Fuselage2 LW_profi le3_rise.stl
Parts_profi le1_rise.stl
Spacer
After that, you can glue fuselage 1 and 2.
After gluing one fuselage part, it is suffi cient
to let some thin CA glue fl ow into the
carbon rod.
thin
Fuselage3 LW_profi le3_rise.stl
medium l.
Fuselage2 LW_profi le3_rise.stl
medium l.
RISE
Fuselage1 LW_profi le3_rise.stl
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
26
Page 27
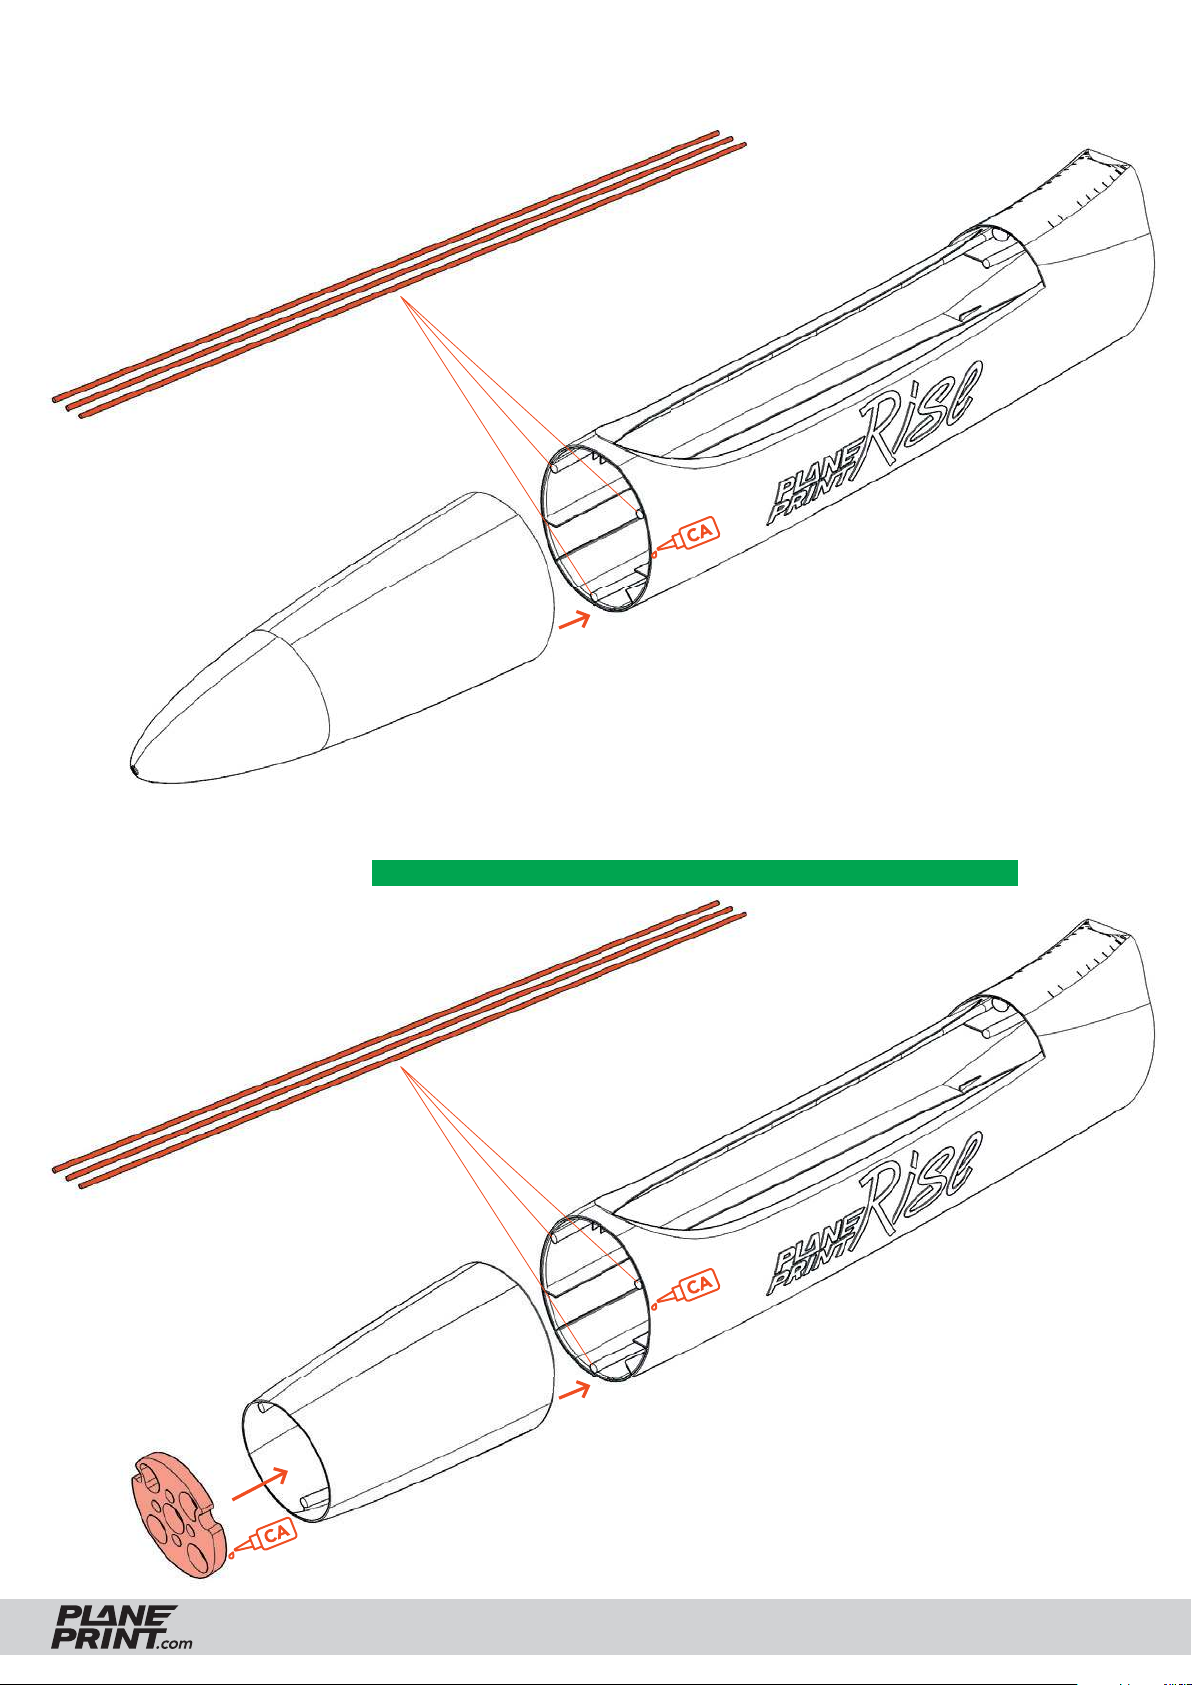
Fuselage assembly – Glider version
Carbon rods Ø1,2*120mm
medium l.
Fuselage1 LW_profi le3_rise.stl
Nose LW_profi le3_rise.stl
Motor version
Carbon rods Ø1,2*120mm
Cut three pieces of carbon rod, adjust the length
so that the nose can be pushed up to the fuselage
1. Then push the rods as far as possible into the
bowden and glue them in place. Then put the
nose on top and glue it.
This parts are only required for the Motor/Spoiler upgrade Kit!
Motormount XXX_profi le1_rise.stl
RISE
medium l.
Nose LW_profi le3_rise.stl
Fuselage1 LW_profi le3_rise.stl
medium l.
Before you glue the motormount into the fuselage, test fi t the motor to make sure everything fi ts
exactly.
The motor mount must be glued very well,
also make sure that the carbon rods reach all the
way to the front!
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
27
Page 28
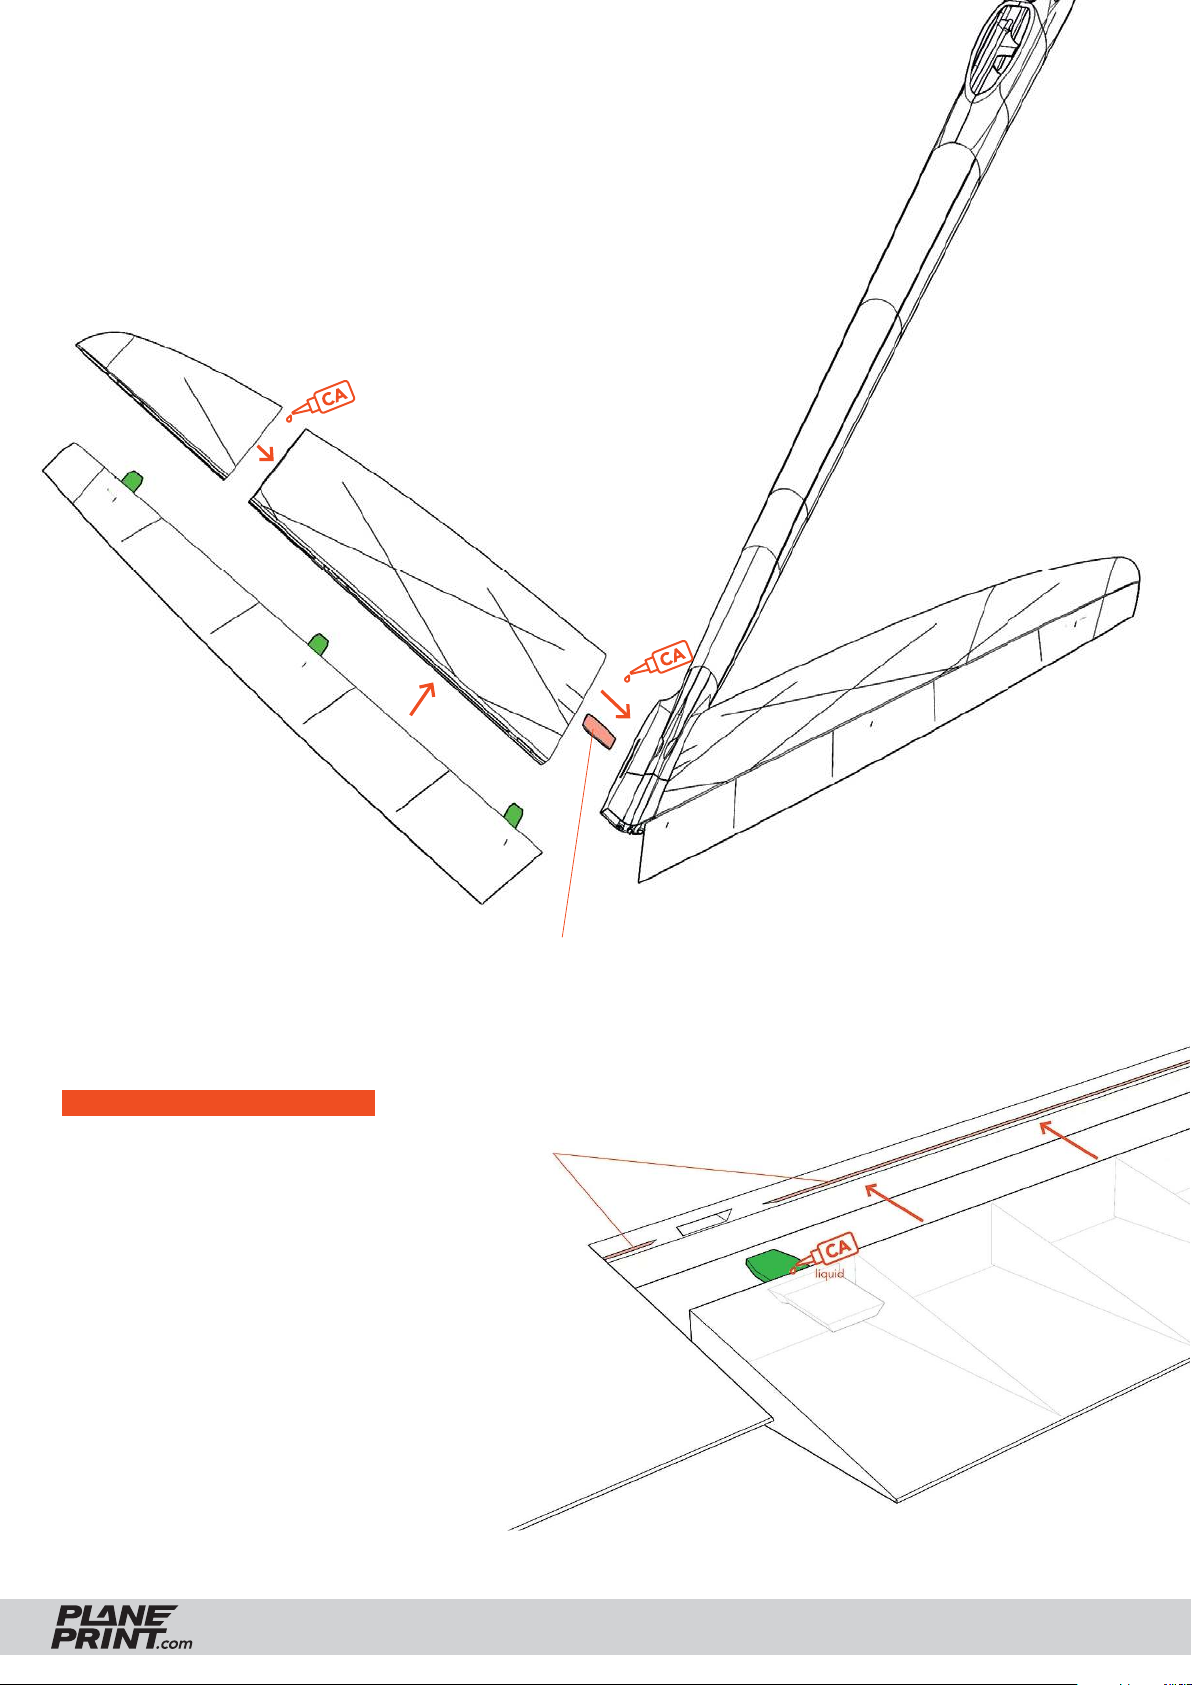
Stabilizer assembly
Glue the parts of the V-tail together as shown.
V-tail2-left LW_profi le3_rise.stl
medium l.
V-tail1-left LW_profi le3_rise.stl
V-tail3-left LW_profi le3_rise.stl
Installation of the TPU Hinges
First insert the hinge into the movable
fl ap and add a drop of liquid CA adhesive
into the gap. Wait for the glue to drain
completely, then spray the activator on it.
medium l.
Parts_profi le1_rise.stl
These spacers ensure the correct
gap distance. Don´t remove!
Then put the fl ap in the wing until the fl ap
touches the spacers and put a drop of CA
glue on the hinge. Wait again for the glue
to run in, and then spray the activator on it.
Do not use too much glue, the fl ap must
move easily!
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
28
Page 29
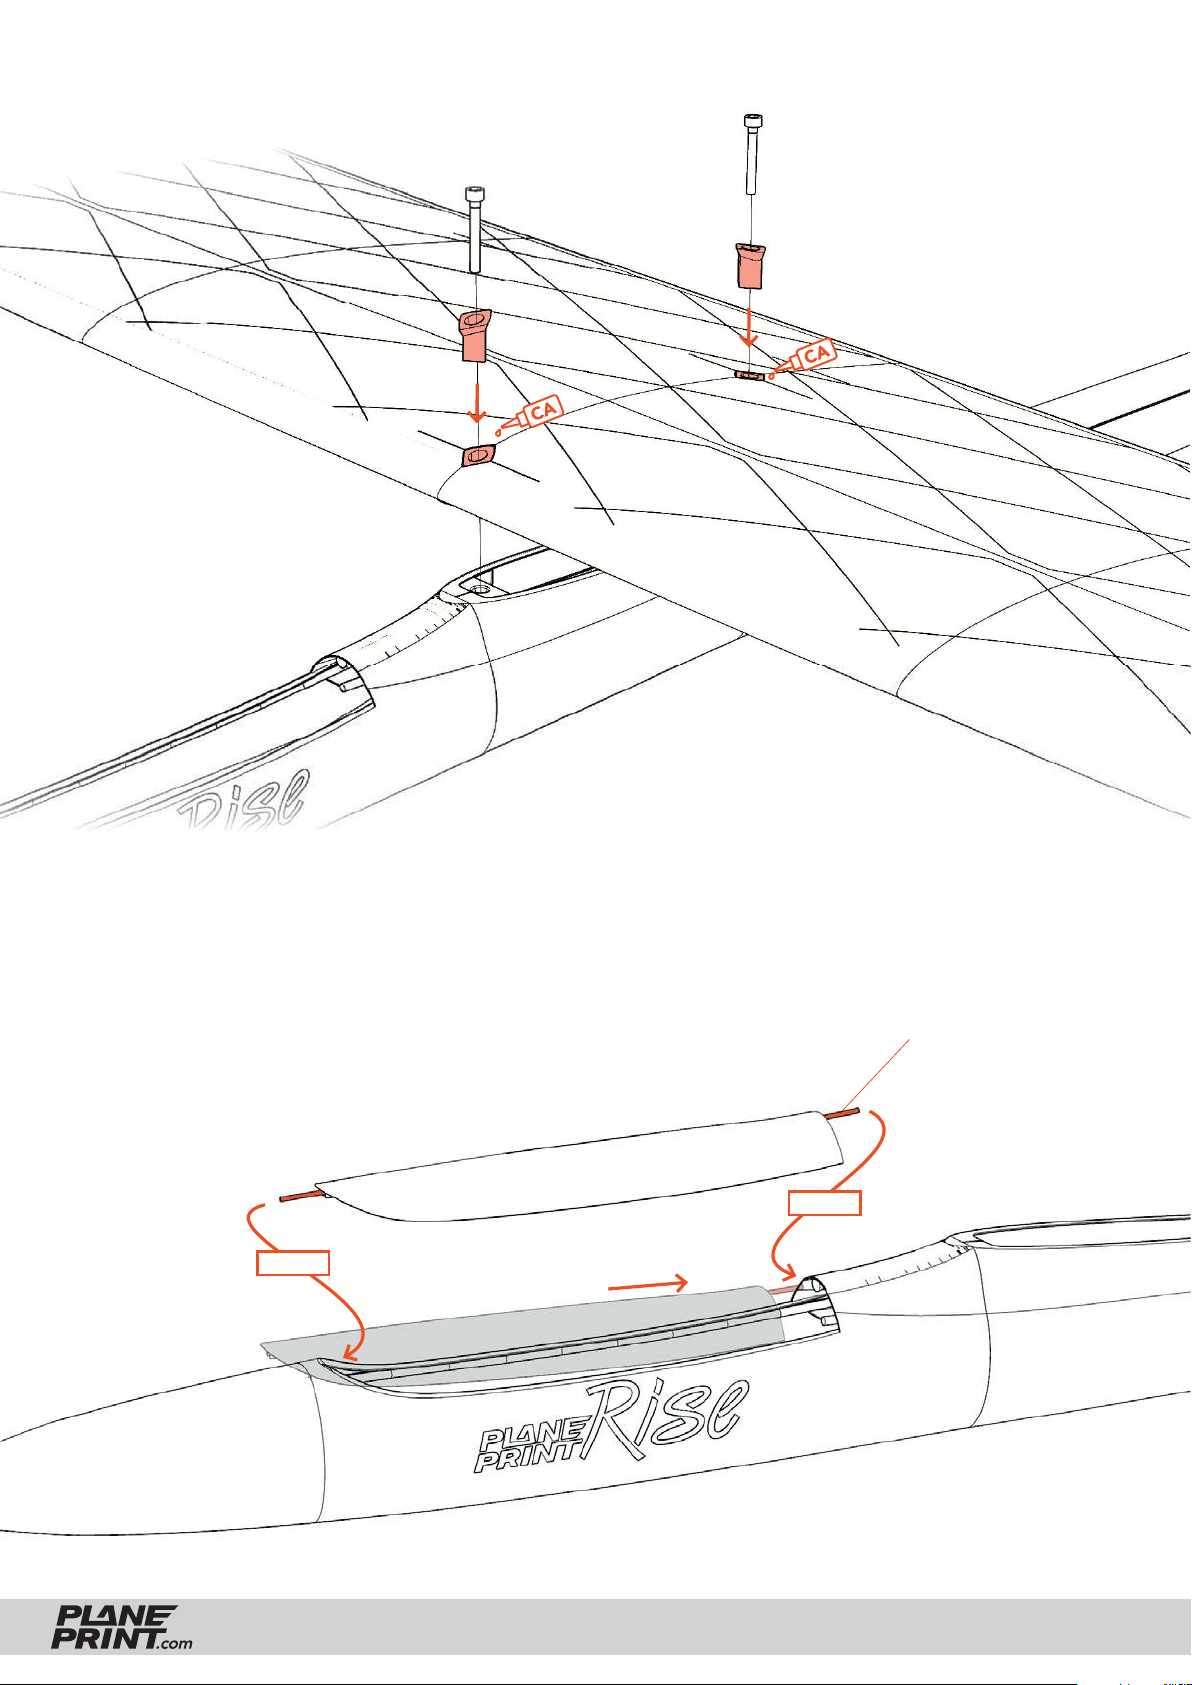
Wing fastening
Wingmount_profi le2_rise.stl
medium l.
medium l.
Canopy fastening
Insert a 165 mm long carbon rod into the bowden of the cap.
To attach it, fi rst insert the front end into the fuselage, push the
canopy slightly forward and then insert it into the fuselage at the back.
The carbon rod should not be glued.
Canopy LW_profi le3_rise.stl
STEP 1
Carbon rod Ø1,2*165mm
STEP 2
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
29
Page 30
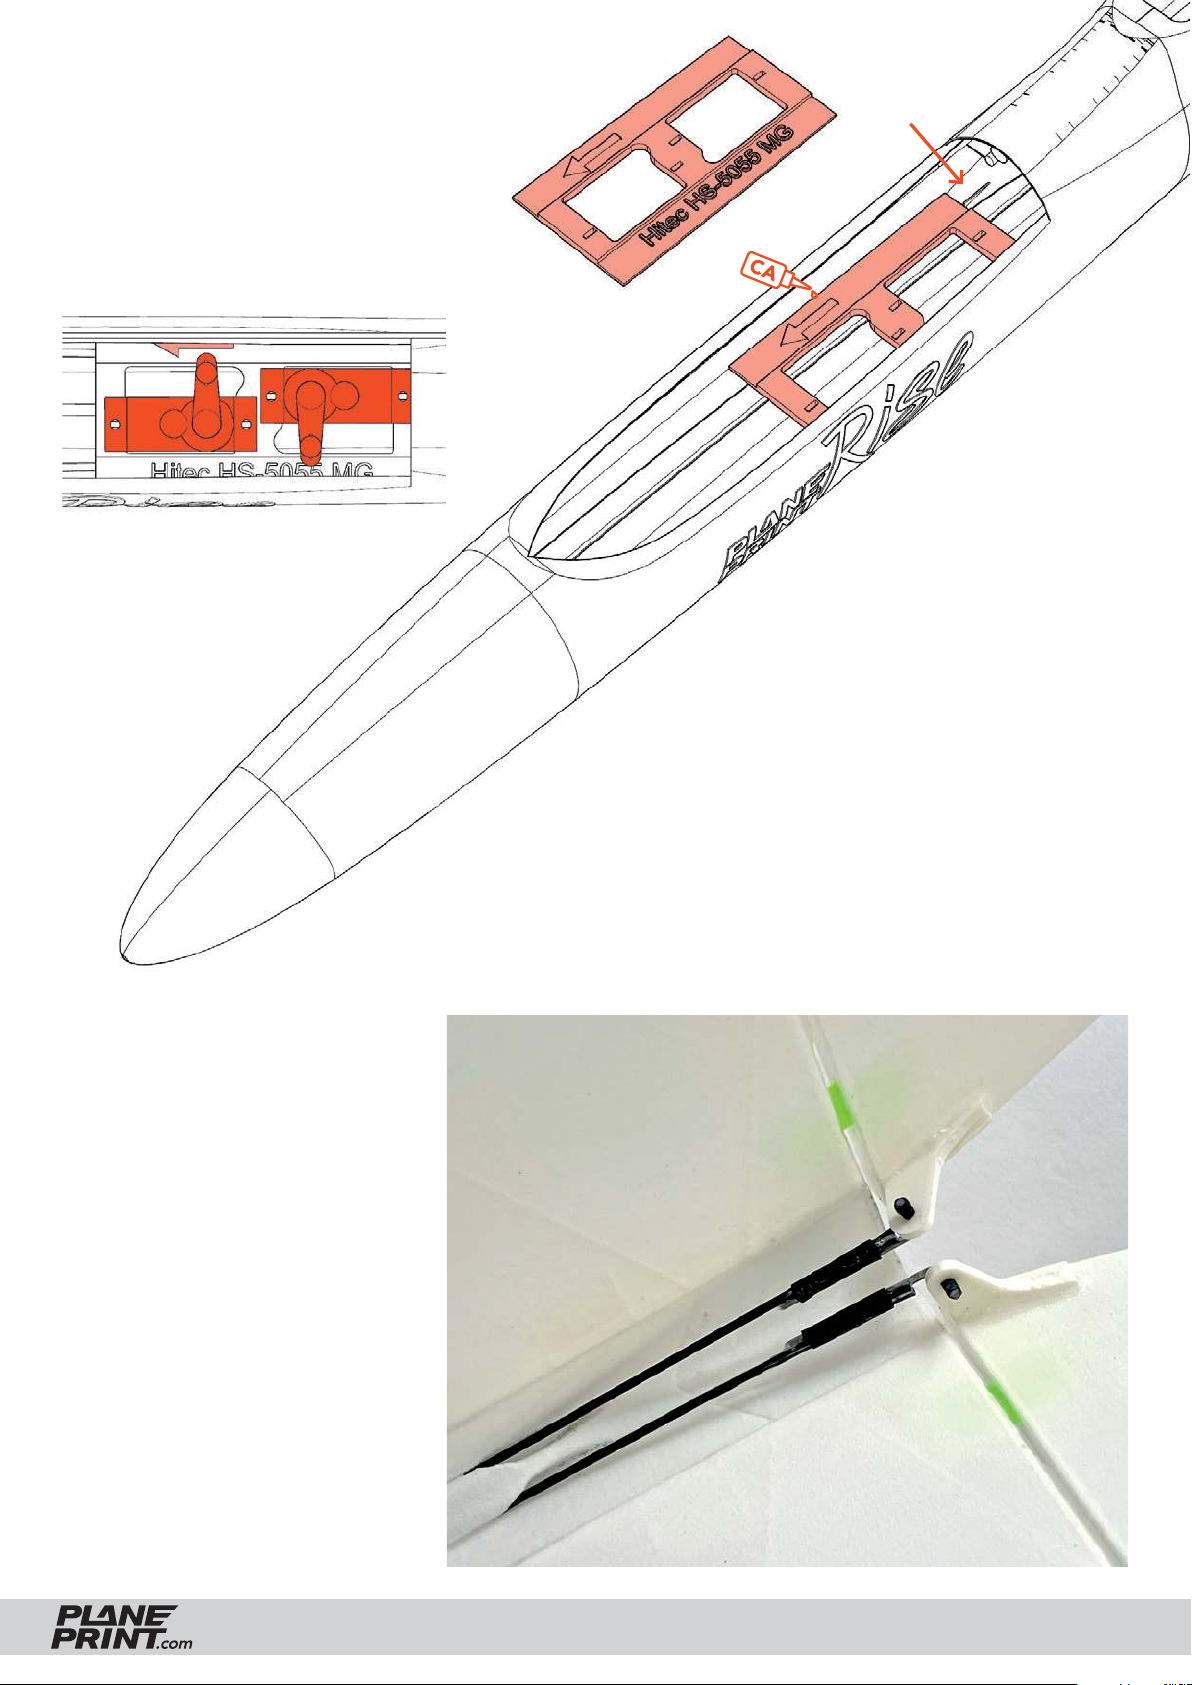
Servo mounting
Stick the servomount in fuselage 1,
push it backwards up to this nub*.
The arrow must point forward.
The servos must be installed in this way:
*
Servomount_HS5055_profi le1_rise.stl
Linkage
For the linkage of the V-tail we
recommend to bend short pieces
of steel wire Ø1mm 90 degrees, to
glue it to the carbon rod Ø1.2mm
(secure it with heat shrink tube).
Secure the linkages to the pin horn
with a short piece of heat shrink
tubing (shrink it beforehand on a
piece of steel wire and then cut
short pieces) and a drop of medium
CA glue.
Mount the adjustable rod
connections to the servos.
RISE
Glue the pin horns
(parts_profi le1_rise.stl)
well as shown here.
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
30
Page 31
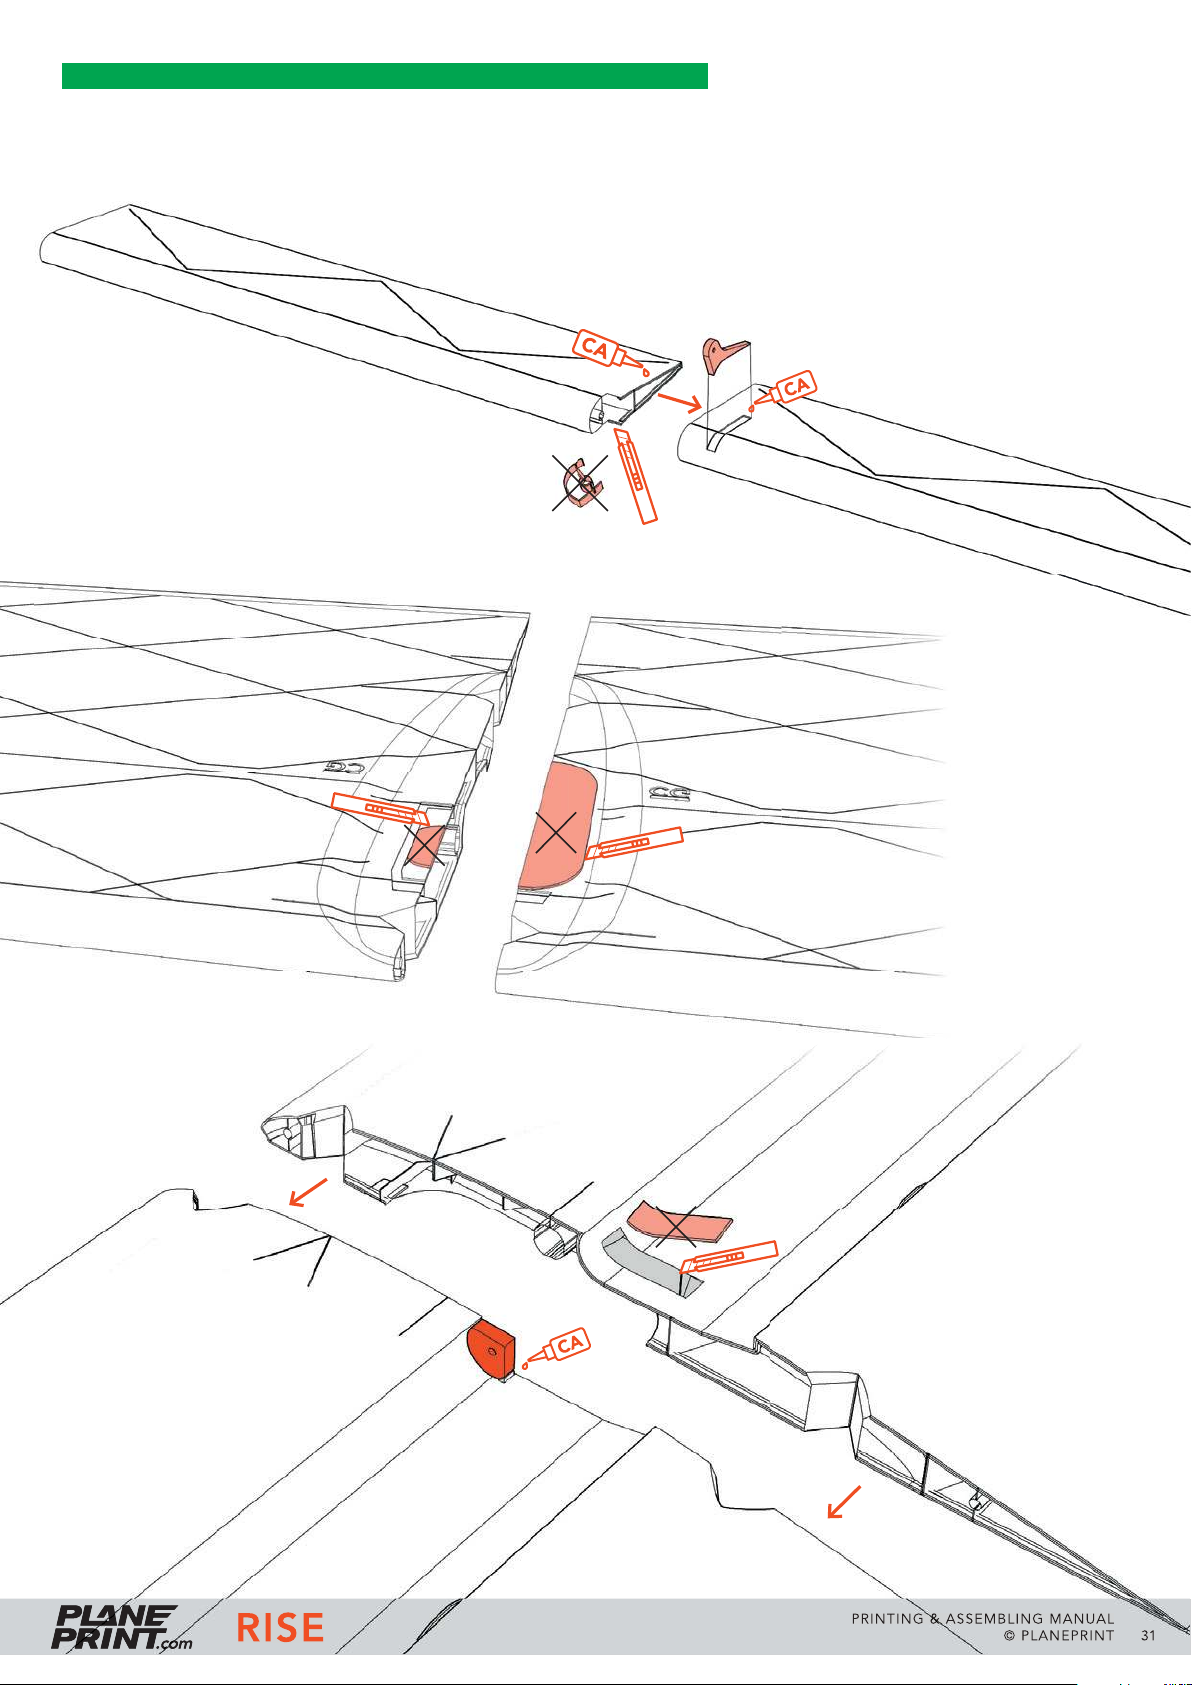
This parts are only required for the Motor/Spoiler upgrade Kit!
Spoiler assembly
Glue the parts of the Spoiler together as shown:
Spoiler mount_profi le1_rise.stl
Spoiler-right LW_profi le3_rise.stl
First remove support:
Wing1 spoiler-right LW_profi le3_rise.stl
medium l.
Remove support
medium l.
Wing1 spoiler-left LW_profi le3_rise.stl
Spoiler-left LW_profi le3_rise.stl
Spoiler mount_profi le1_rise.stl
RISE
medium l.
Remove support
See Wings assembly
instructions on page 22.
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
31
Page 32
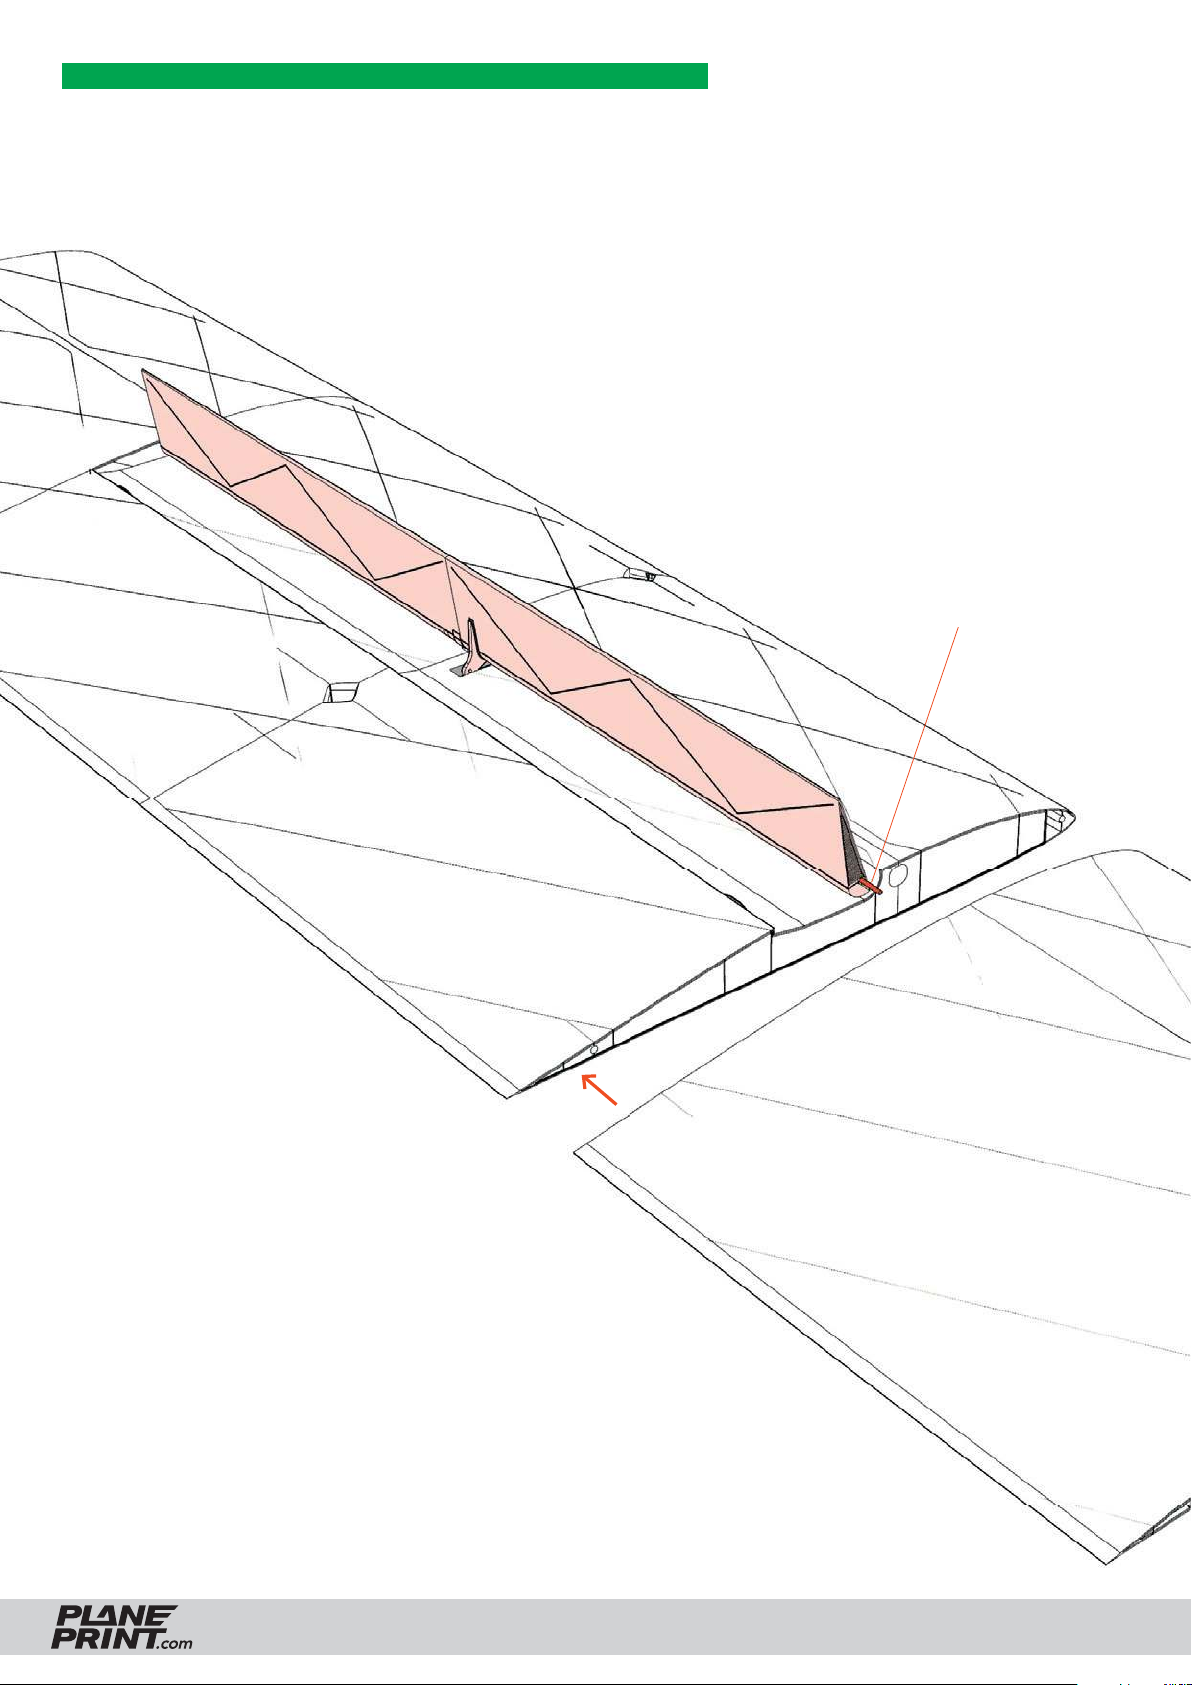
This parts are only required for the Motor/Spoiler upgrade Kit!
Spoiler assembly
Wing2-left LW_profi le3_rise.stl
Wing1 spoiler-left LW_profi le3_rise.stl
Cut a 404mm long carbon rod Ø1,2mm and mount
the spoilers as shown in the picture. In the parts
Wing2 are short bowden for the swivel integrated.
Carbon rod Ø1,2*404mm
Wing1 spoiler-right LW_profi le3_rise.stl
See Wings assembly instructions on page 22.
Wing2-right LW_profi le3_rise.stl
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
32
Page 33
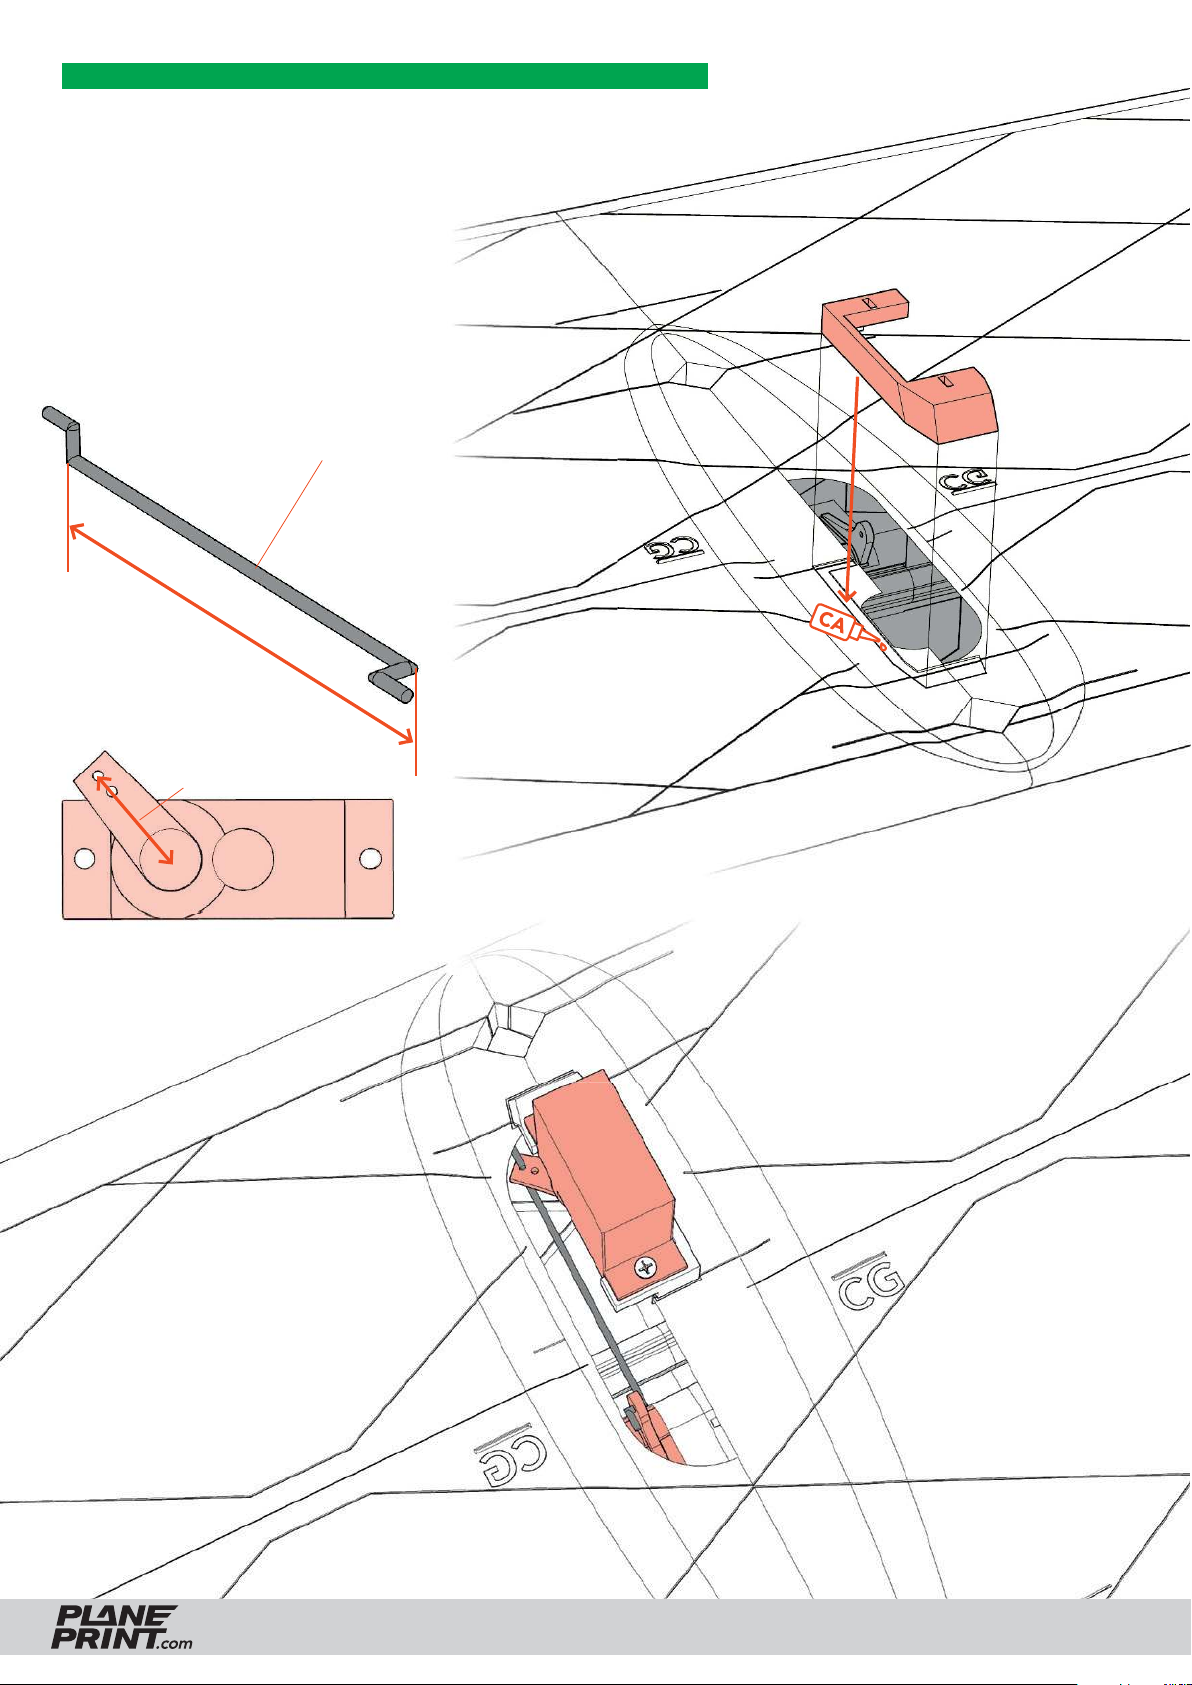
This parts are only required for the Motor/Spoiler upgrade Kit!
Spoiler linkage
Glue the servo mount to the wing.
Bend a steel wire Ø1mm as
shown. The distance between the
axes should be exactly 42mm.
Steel wire Ø1mm
42mm
maximum 10 to 11mm
Spoiler mount_profi le1_rise.stl
medium l.
Mount the servo as shown:
Wing1 spoiler-right LW_profi le3_rise.stl
Wing1 spoiler-left LW_profi le3_rise.stl
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
33
Page 34
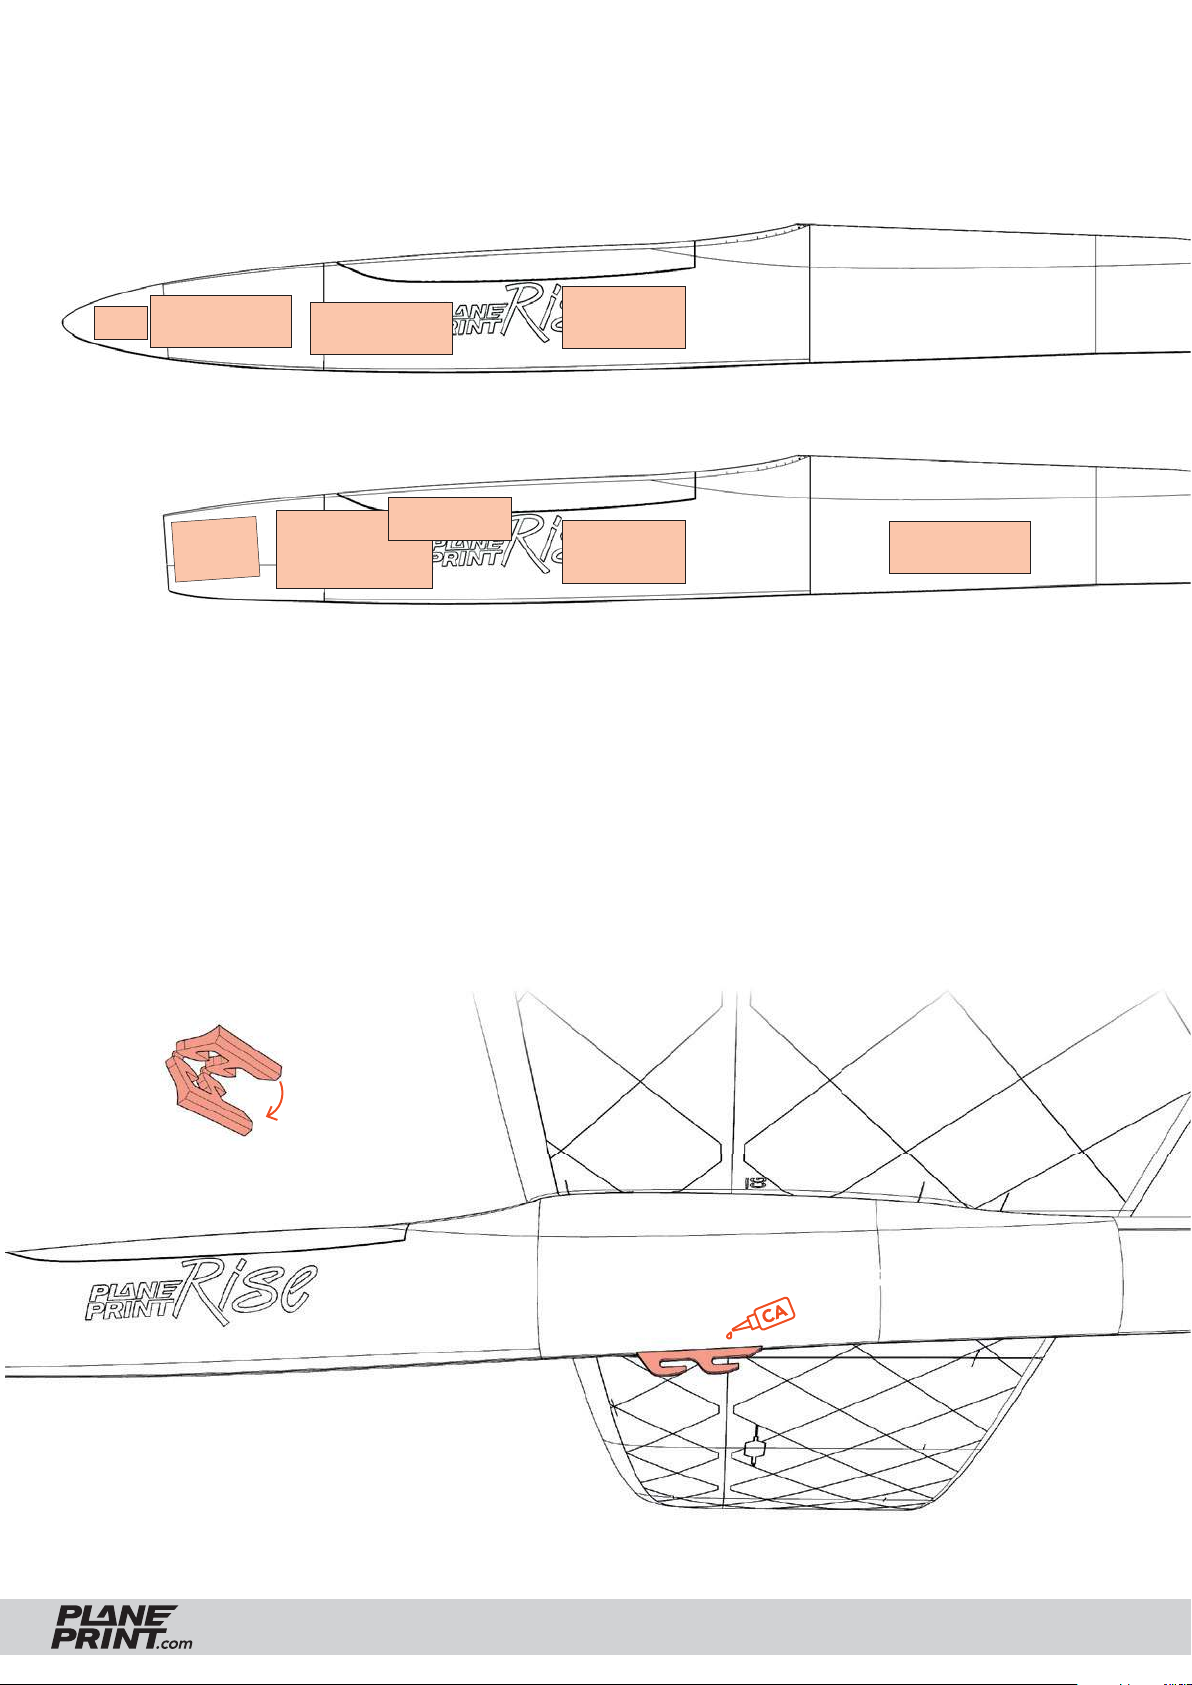
RC components
Glider version
Lead
Battery
Receiver
Servos
Motor version
Controller
Motor
Battery
Servos
Launch Hook – Glider version
The launch hook is only recommended for experienced pilots, because the
wings made of LW-PLA are very soft and must only be loaded very gently!
The rear hook should be positioned about 5mm in front of the CG.
Receiver
RISE
medium l.
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
34
Page 35
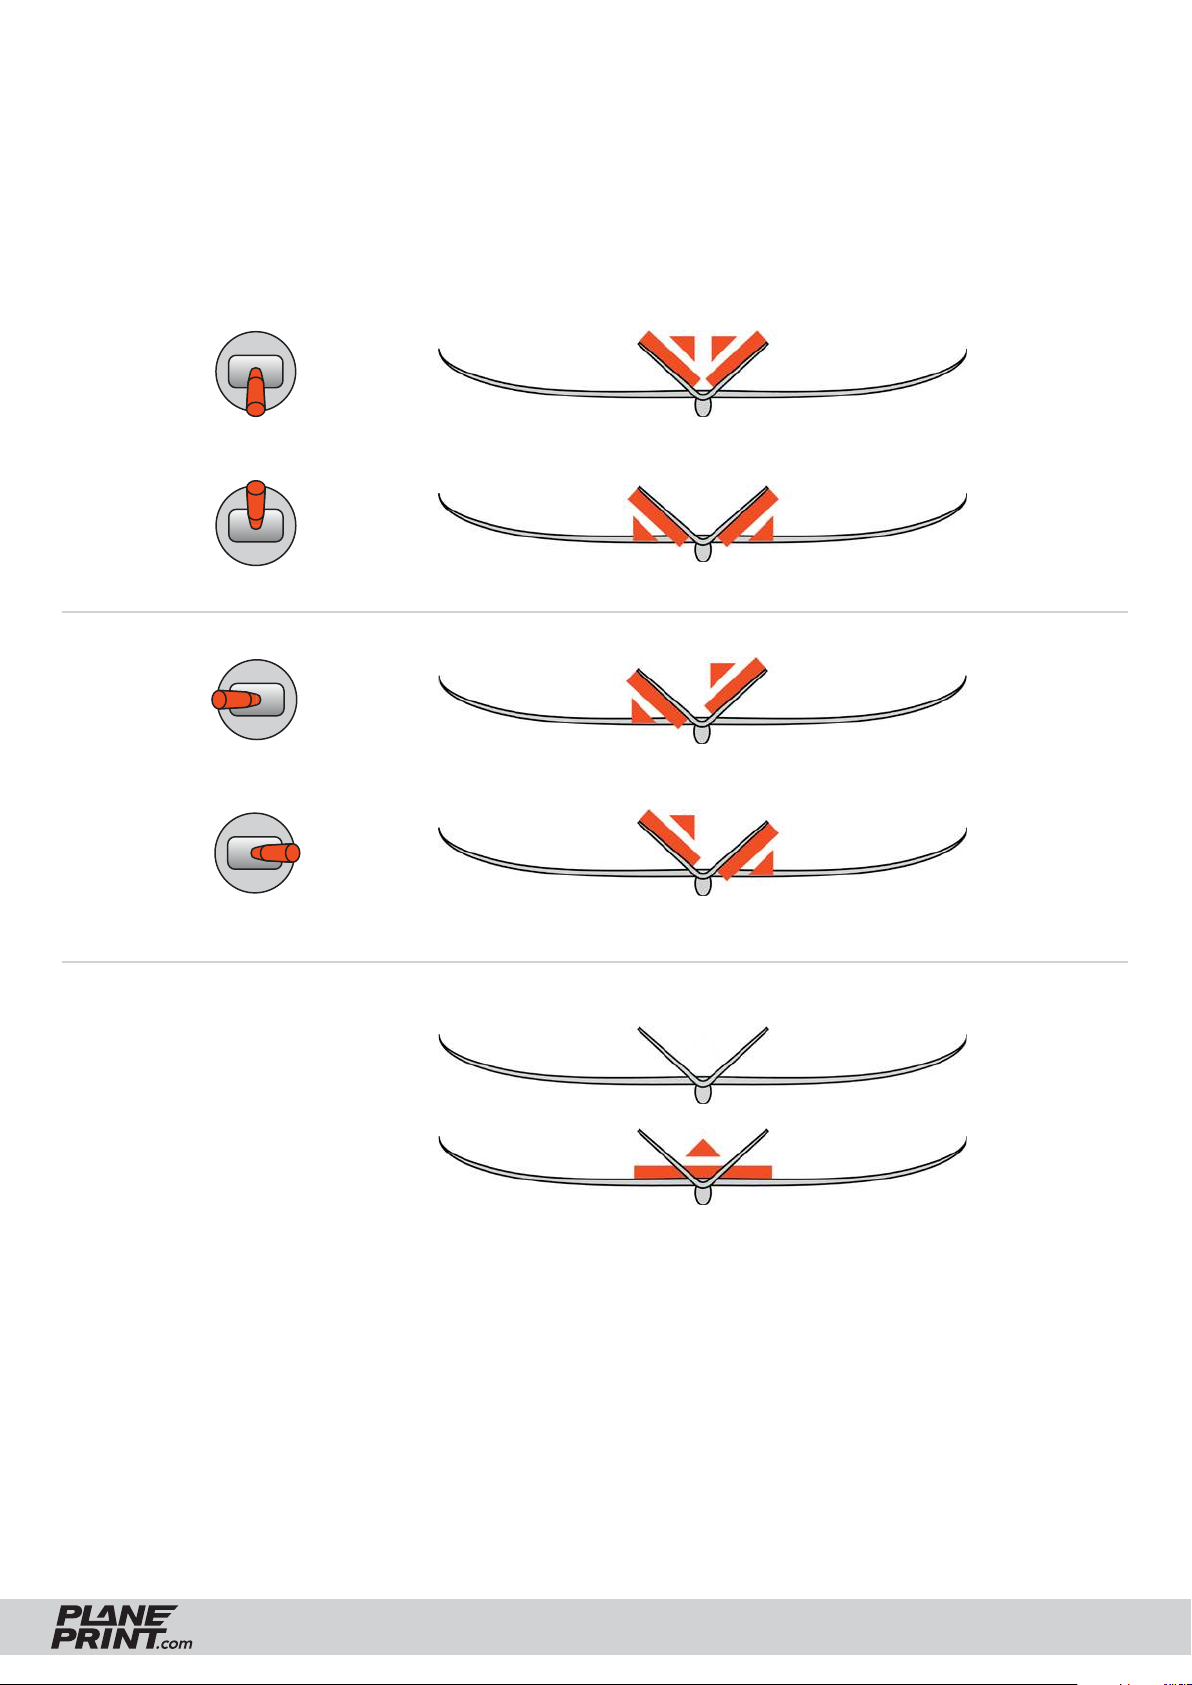
Control Direction Test
Turn on the transmitter and connect the battery. When checking
the control directions, look at the aircraft from behind.
ELEVATOR
RUDDER
SPOILER 0 %
SPOILER 100 %
Motor version
We recommend that you put the engine on a switch and the spoiler on the gas stick.
PRINTING & ASSEMBLING MANUAL
RISE
© PLANEPRINT
35
Page 36
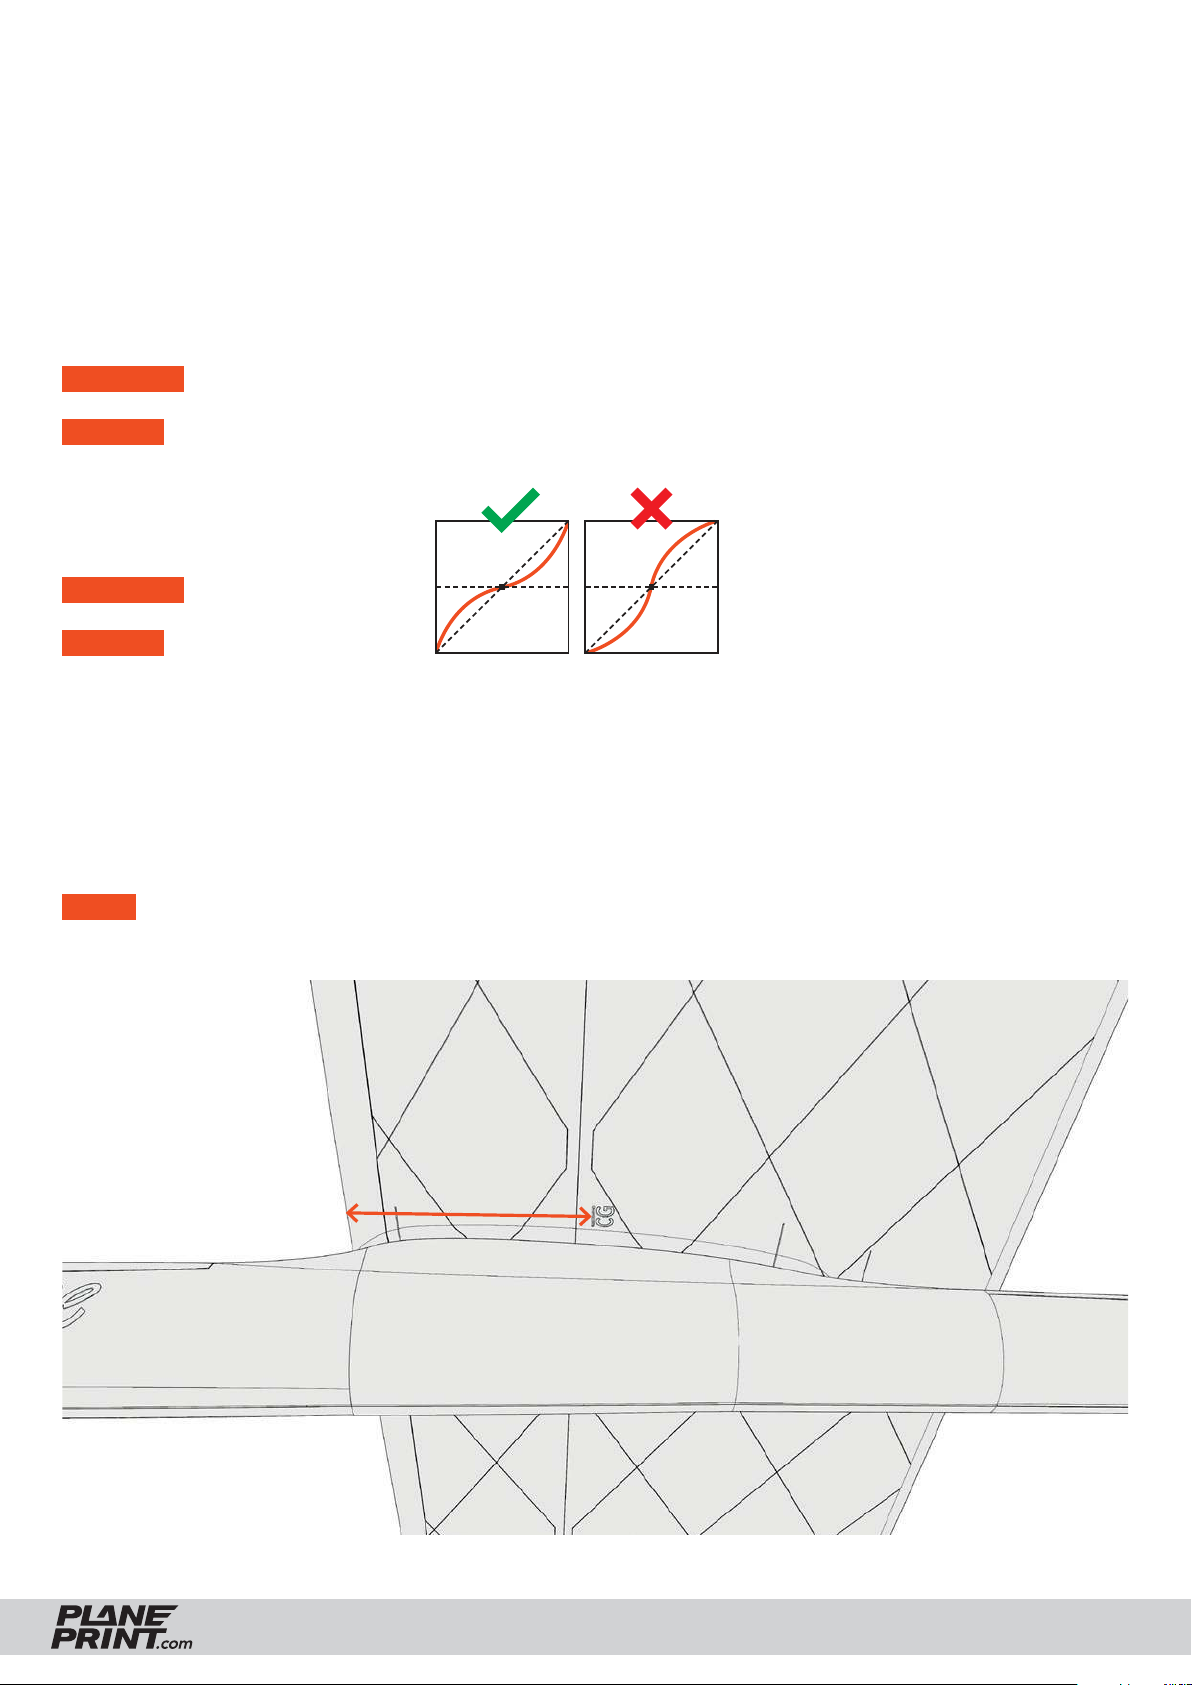
SETTINGS FOR FLYING
After installing the electronics and setting up the transmitter, check that the control surfaces are aligned
correctly. Set the transmitter trim to zero. Align all rudders to zero position. Change the position of the
moving parts by changing the length of the linkage from the servo arm to the control horn. In-flight
adjustments can be made later with the trim.
Setting the servo travel
ELEVATOR up: 14 mm, down: 14 mm
RUDDER left: 14 mm, right: 14
Expo setting
ELEVATOR 20 %
RUDDER 20 %
(for some remote controls a minus
has to be in front of the number)
Center of Gravity (CG)
The aircraft must balance 76 mm/3 inches behind the leading edge (see markings on the fuselage).
For the first flight we recommend to move the center of gravity about 5 mm/0.2 inches further forward.
NOTE The CG of 76 mm is the setting we tested with the best flight characteristics.
If you are not yet an expert pilot, your CG should be a few millimeters further forward, not further back!
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
36
Page 37
Flight timer
Flight time will vary depending on the battery size. Expect 5 minutes under normal circumstances; however,
it may be possible to fly for much longer. It is a good idea to be conservative with the flight timer until you gain
experience with your airplane.
TECHNICAL SPECIFICATIONS
WINGSPAN 2000 mm/78.7 inches
LENGHT 1198 mm/47 inches
FLIGHT WEIGHT Glider version 650 grams
Motor version 680 grams (with 3S/640MaH-Battery)
RISE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
37
Page 38
AGE RECOMMENDATION 14+
NOT FOR CHILDREN UNDER 14 YEARS.
THIS IS NOT A TOY!
By using the download data, an RC model airplane, called
„model“ for short, can be manufactured using a 3D printer.
As a user of this model, only you are responsible for safe
operation that does not endanger you or others, or that
does not damage the model or property of others.
PLANEPRINT.com assumes no responsibility for damage to
persons and property caused by pressure, transport or use
of the product. Filaments, printing supplies, hardware or
consumables that can not be used after faulty 3D printing
will not be replaced by PLANEPRINT.com in any way.
When operating, always keep a safe distance from your
model in all directions to avoid collisions and injuries.
This model is controlled by a radio signal. Radio signals can
be disturbed from outside without being able to influence
it. Interference can lead to a temporary loss of control.
Always operate your model on open terrains, far from cars,
traffic and people.
Always follow the instructions and warnings for this product
and any optional accessories (servos, receivers, motors,
propellers, chargers, rechargeable batteries, etc.) carefully.
Avoid water contact with all components that are not specially designed and protected. Moisture damages the electronics.
Never take an item of the model or accessory in your mouth
as this can lead to severe injuries or even death.
Never operate your model with low batteries in the transmitter or model.
Always keep the model in view and under control.
Use only fully charged batteries.
Always keep the transmitter switched on when the model
is switched on.
Always remove the battery before disassembling the model.
Keep moving parts clean and dry at all times.
Always allow the parts to cool before touching them.
Always remove the battery after use.
Make sure that the Failsafe is properly set before the flight.
Keep all chemicals, small parts and electrical components
out of the reach of children.
We develop our models to the best of our knowledge and belief.
We accept no liability for consequential damage and injuries
caused by improper use. Please be careful when handling
motors, batteries and propellers and only move your model with
insurance and in approved places!
Never operate the model with damaged wiring.
Never touch moving parts.
© PLANEPRINT.com, A-6021 Innsbruck, Conradstraße 6, [email protected]
© Design STL files by René Marschall • Layout: marschall designlab, marschall.cc
 Loading...