

Page 1
EAGLE
PRINTING & ASSEMBLING MANUALP R I N T I N G & A S S E M B L I N G M A N U A L
NOTE: Slicing only
works with CURA!
You can fi nd the STL data
at www.planeprint.com
Page 2
PRINTING THE PARTS – PRINTING PROFILES
You may wonder why this 3D model is suitable exclusively for CURA right?
The most important thing about small RC model airplanes is always the ratio of size to weight.
The lighter a model is, the better its flight characteristics and also the flight time is significantly
increased.
With our unique design process, we manage to make Weights relevant items in a true 1-wall prin-
ting process for the outer skin but also for the filling offer. So we save weight while maintaining the
necessary stability.
Here we show you how to get started from a standard CURA profile Make settings. For this model
we only need 4, easy to create profiles.
It is absolutely necessary to observe the information provided by PLANEPRINT.com in order:
to slice the component correctly. However, it may make sense to perfect your 3D printing by
additionally performing several hiring activities depending on your printer and the filament used.
For slicing all Planeprint
models, four profiles have
to be created in Cura:
PROFILE P1_fullbody
PROFILE P2_hollowbody
PROFILE P3_surface
PROFILE P4_flex
You can find the description at
www.planeprint.com/print
IMPORTANT FOR
THE 1-WALL-PRINT!
In order to print airfoils of the lowest possible weight with high stability, it is necessary to print with only one wall line (Nozzle 0.4
mm). Decisive here is the adhesion between
the layers! To achieve this, you must print at
a much higher temperature than normal. As
a guideline, 230 ° C is a good starting point.
The parts-cooling fan should be set to 0% or
a maximum of 20%. Since not every printer
works the same, it may be necessary to make
small adjustments to these settings.
The development of a complex, airworthy RC flight model to express on any standard 3D printer is
a very complex and extensive process. Therefore, we appeal to your fairness not to forward the STL
data you have acquired to third parties. Our STL files are provided with indelible copyright watermarks that can be verified at any time.
Thank you for your understanding and have fun with your PLANEPRINT MODEL!
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
2
Page 3
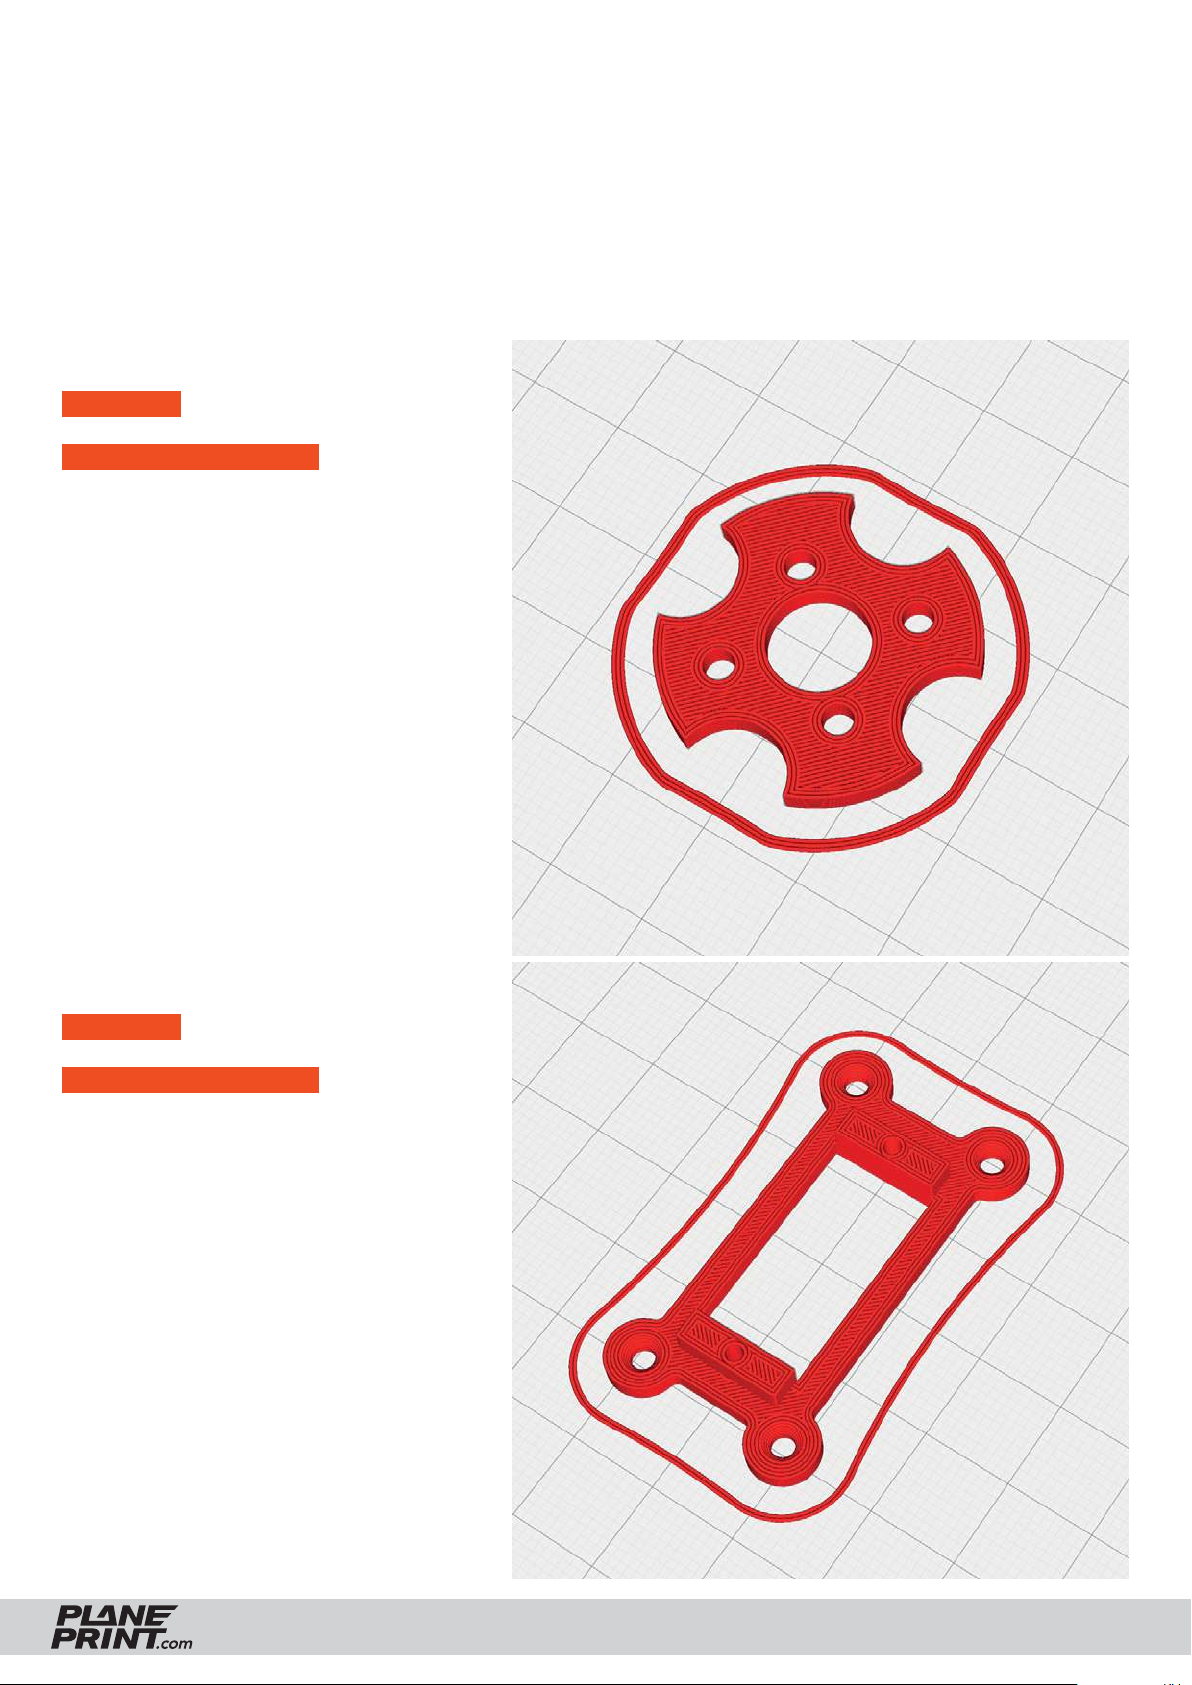
PROFILE P1_FULLBODY
The following parts must be sliced with the PROFILE P1_FULLBODY.
Please note the additional settings for the individual parts!
eagle-Motormount-profile1.stl
MATERIAL PLA, Weight: ~ 2 g
ADDITIONAL SETTINGS
None required
eagle-Servomount-profile1.stl
MATERIAL PLA, ~ 2 g
ADDITIONAL SETTINGS
None required
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
3
Page 4
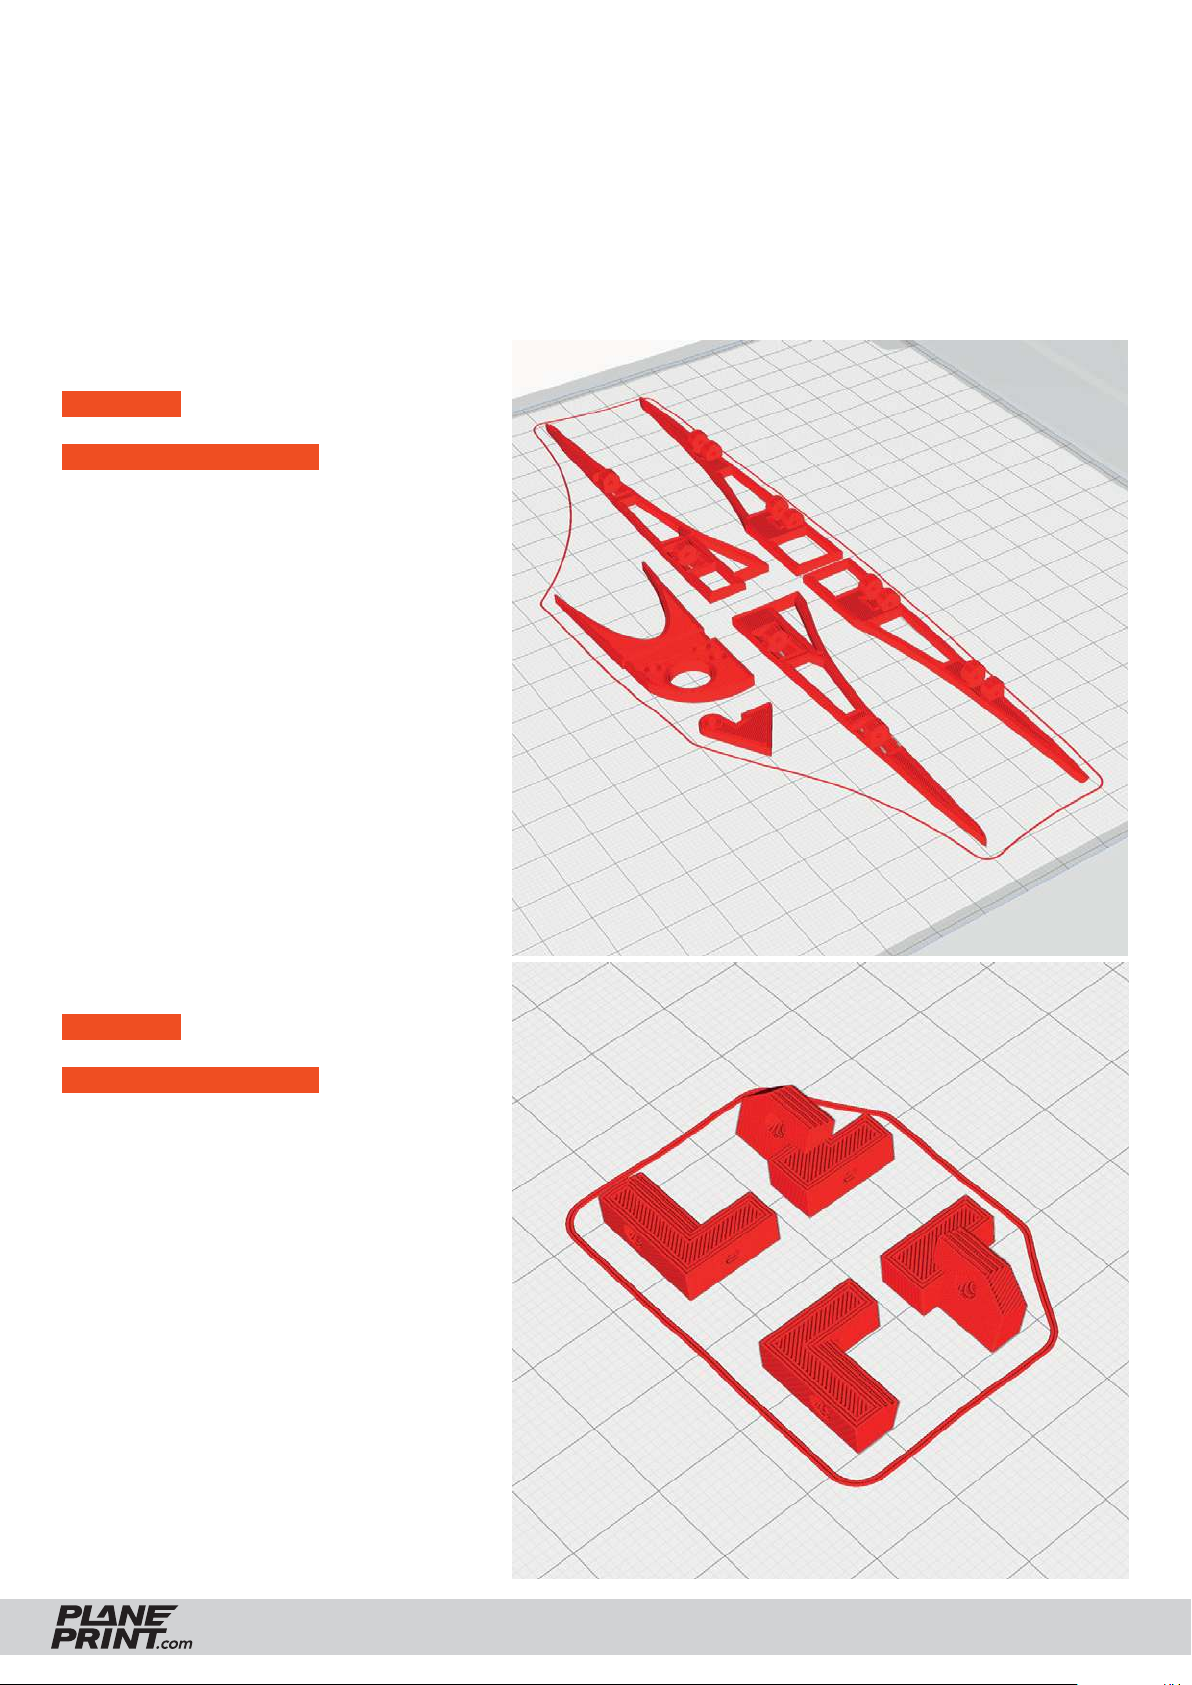
PROFILE P1_FULLBODY
The following parts must be sliced with the PROFILE P1_FULLBODY.
Please note the additional settings for the individual parts!
eagle-Tail hinge-profile1.stl
MATERIAL PLA, ~ 7 g
ADDITIONAL SETTINGS
None required
eagle-wingservo_xxx-profile1.stl
MATERIAL PLA, ~ 2 g
ADDITIONAL SETTINGS
None required
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
4
Page 5
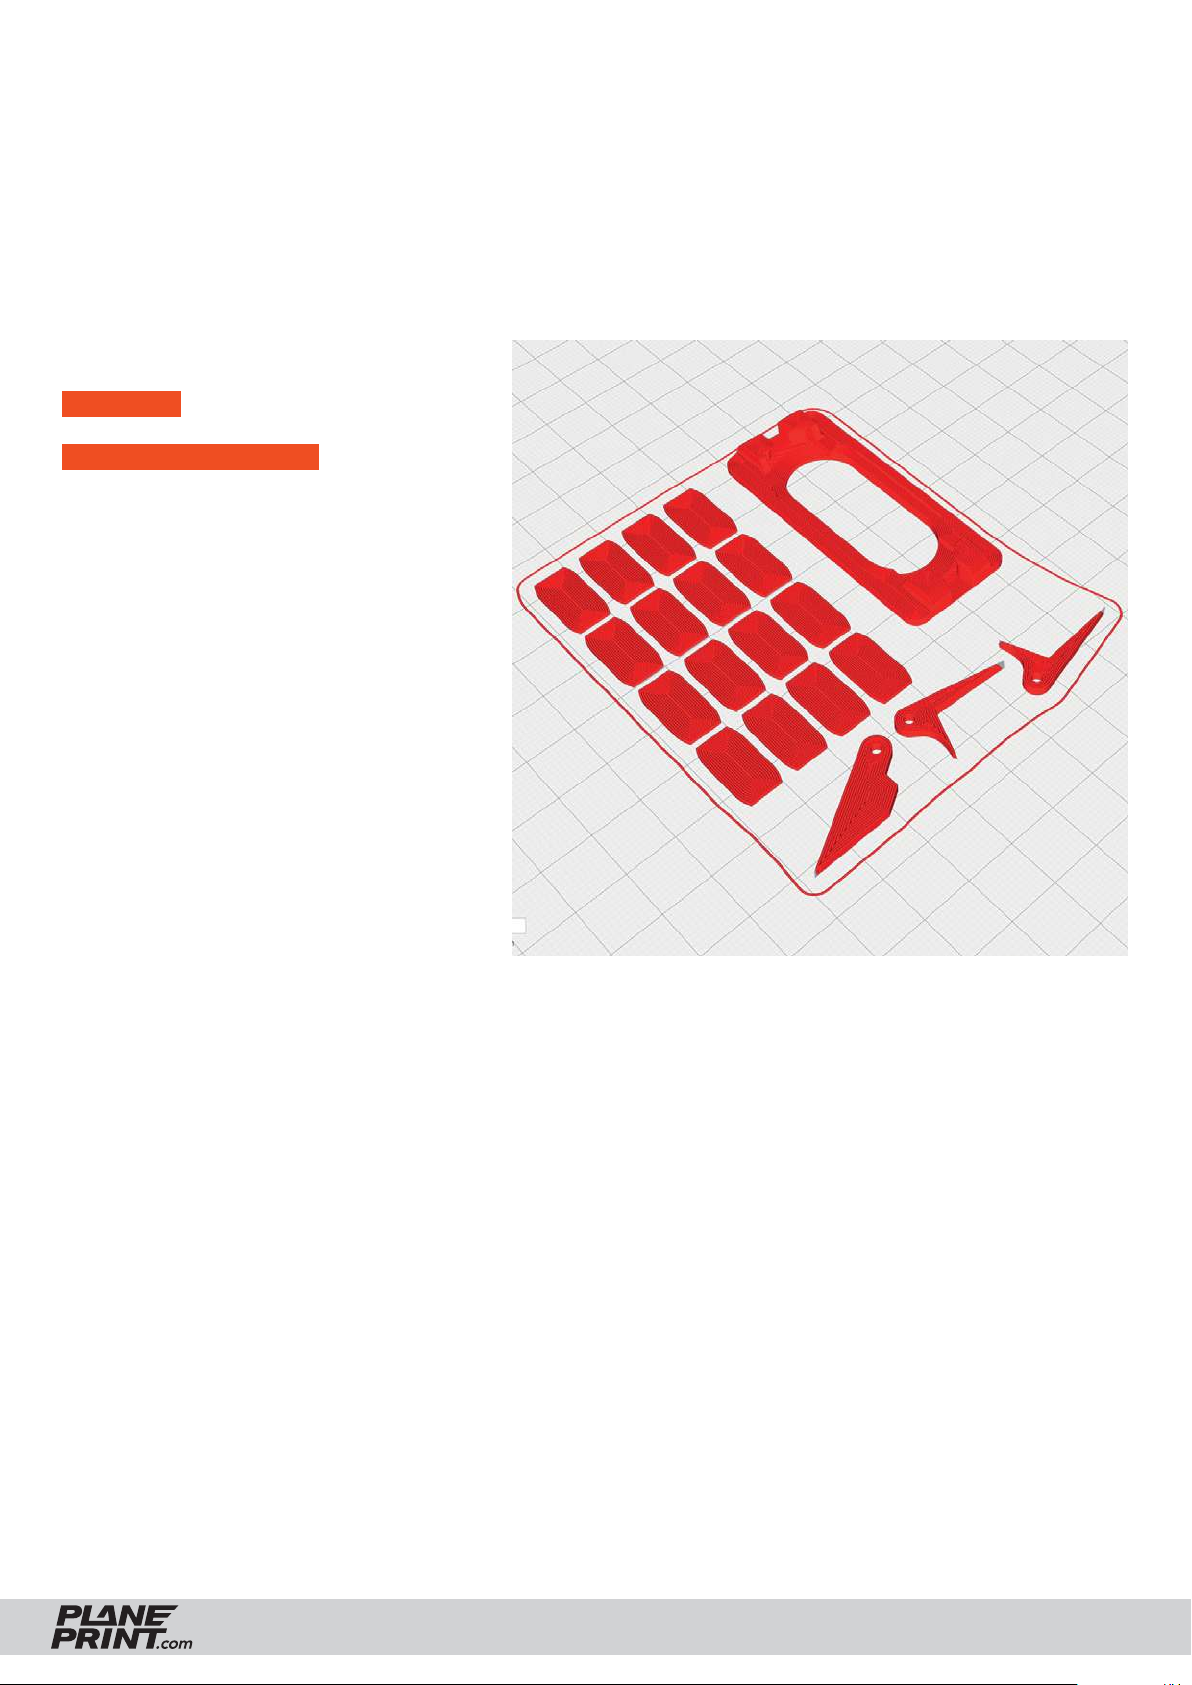
PROFILE P1_FULLBODY
The following parts must be sliced with the PROFILE P1_FULLBODY.
Please note the additional settings for the individual parts!
eagle-Parts-profile1.stl
MATERIAL PLA, ~ 5 g
ADDITIONAL SETTINGS
None required
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
5
Page 6
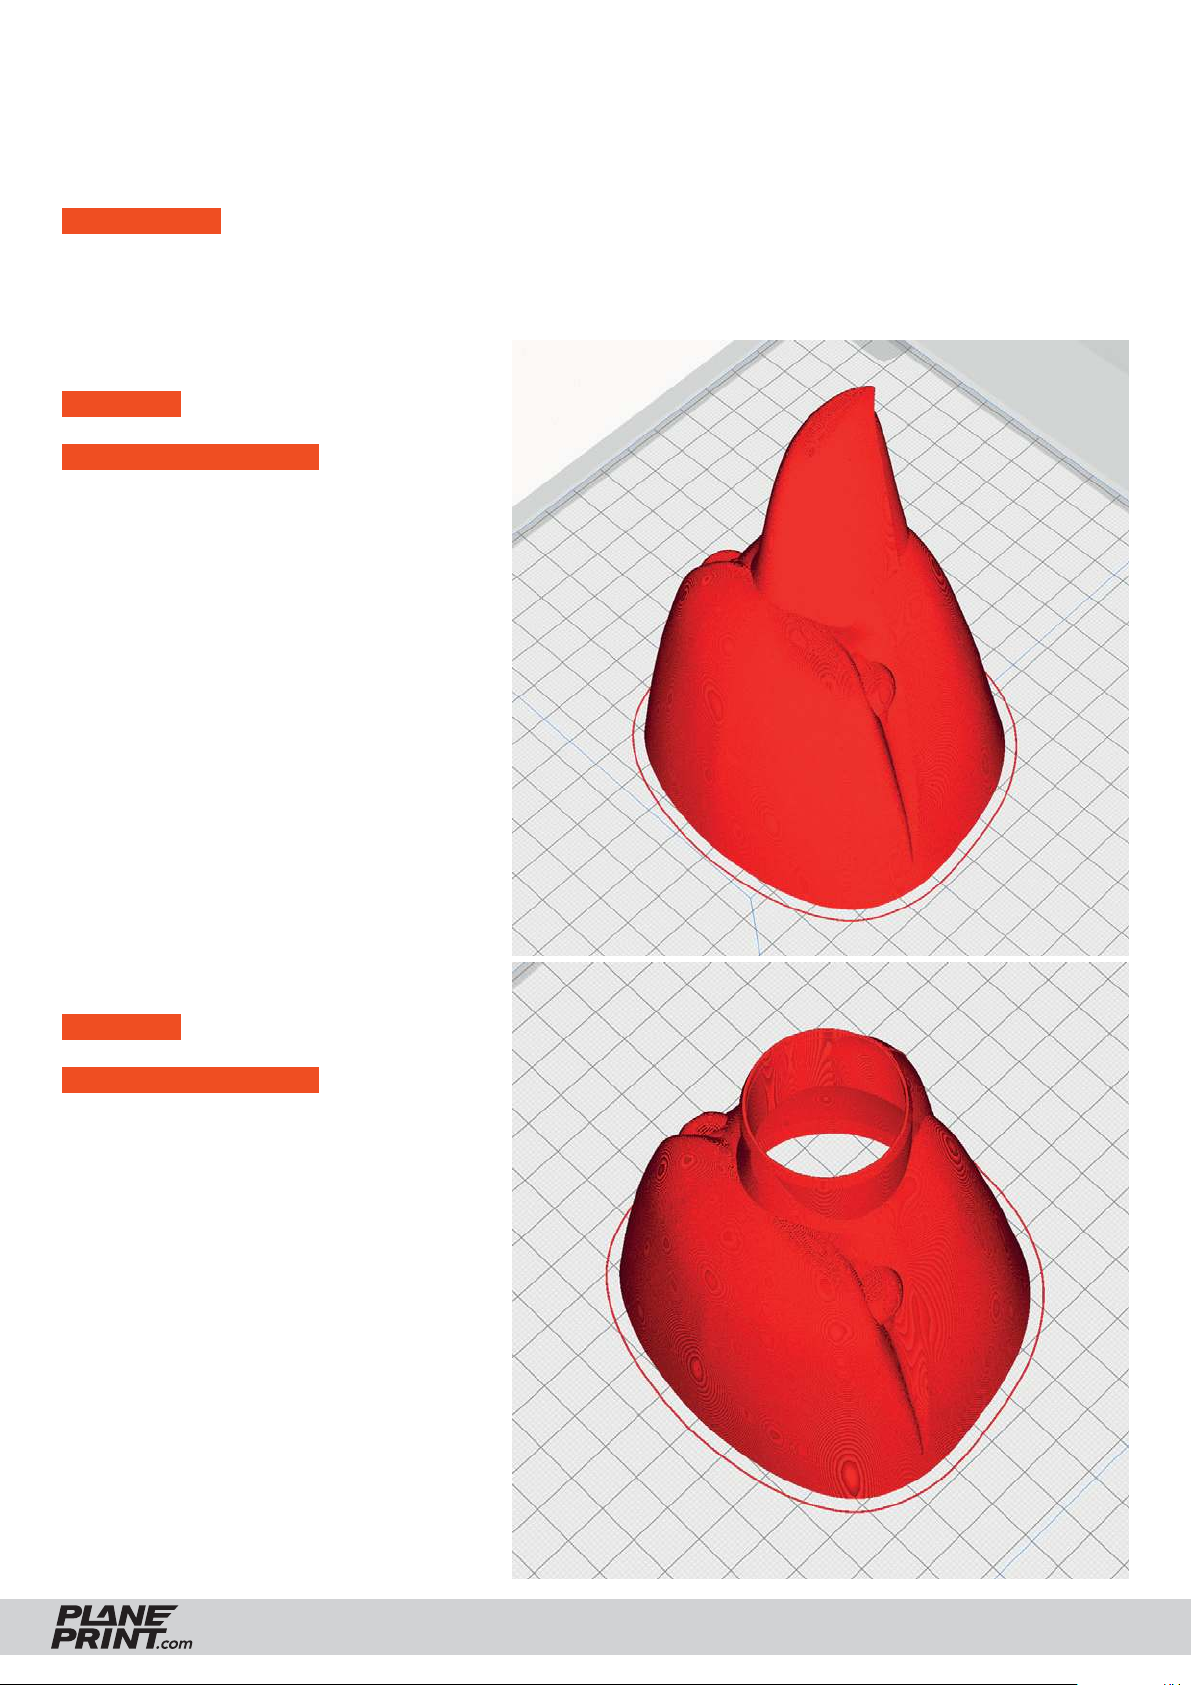
PROFILE P3_SURFACE normal PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Head-profile3.stl
MATERIAL PLA, ~ 28 g
ADDITIONAL SETTINGS
None required
eagle-Motorhead-profile3.stl
MATERIAL PLA, ~ 28 g
ADDITIONAL SETTINGS
None required
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
6
Page 7
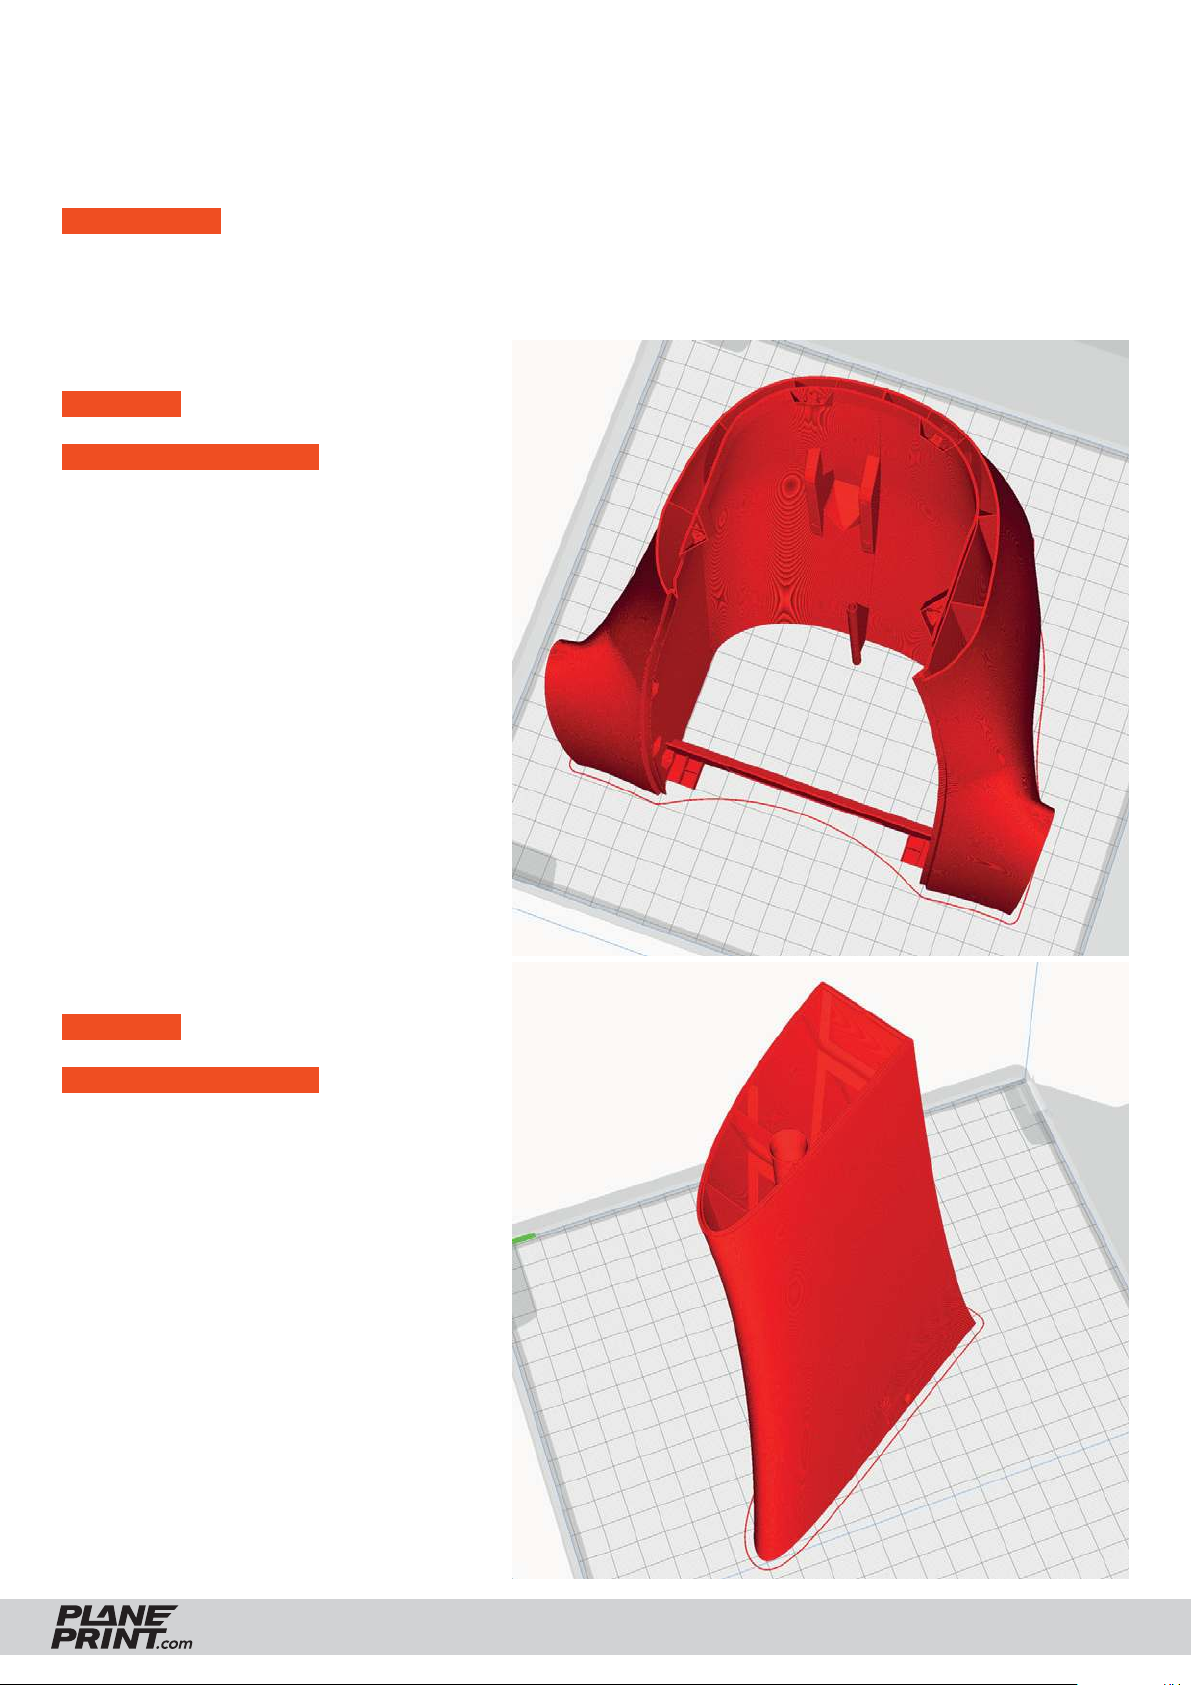
PROFILE P3_SURFACE normal PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Body1-profile3.stl
MATERIAL PLA, ~ 88 g
ADDITIONAL SETTINGS
None required
eagle-Wing1-left/right-profile3.stl
MATERIAL PLA, ~ 37 g
ADDITIONAL SETTINGS
None required
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
7
Page 8
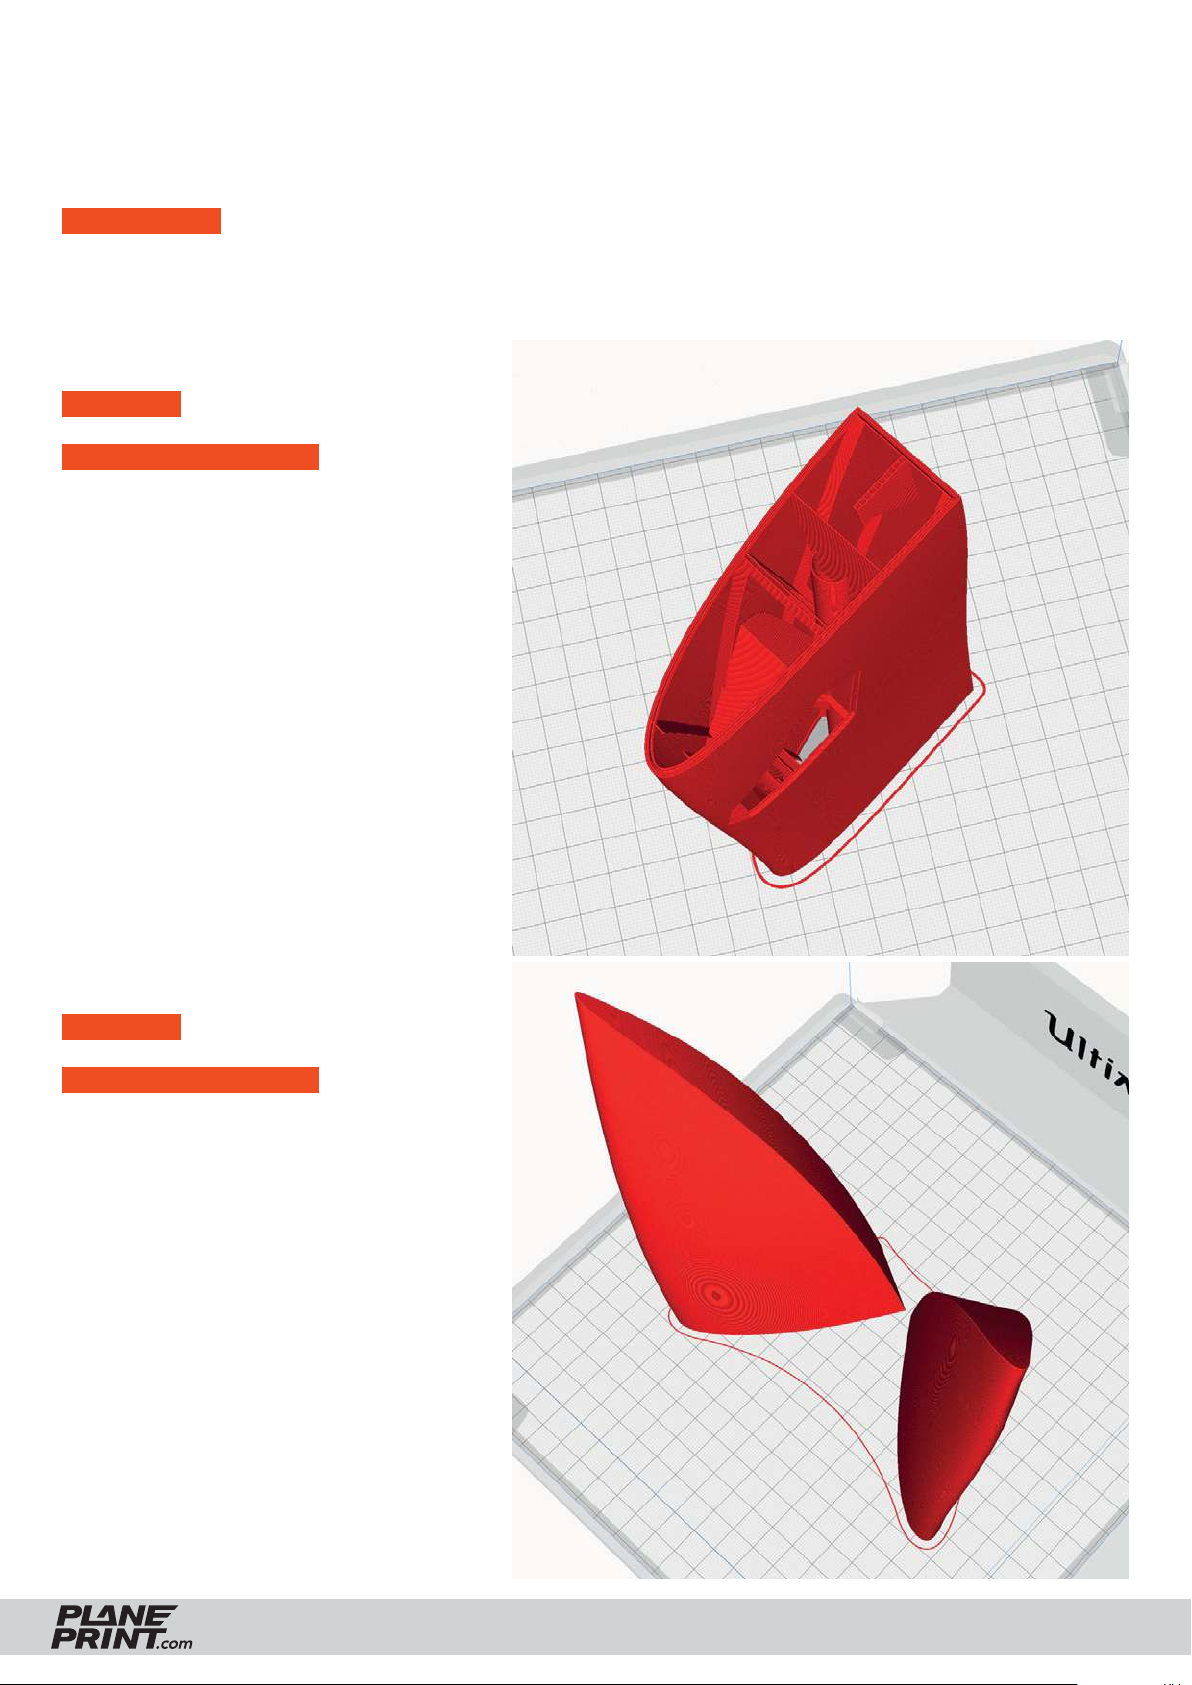
PROFILE P3_SURFACE normal PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Wing2-left/right-profile3.stl
MATERIAL PLA, ~ 33 g
ADDITIONAL SETTINGS
None required
eagle-Wing3-both-profile3.stl
MATERIAL PLA, ~ 33 g
ADDITIONAL SETTINGS
None required
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
8
Page 9
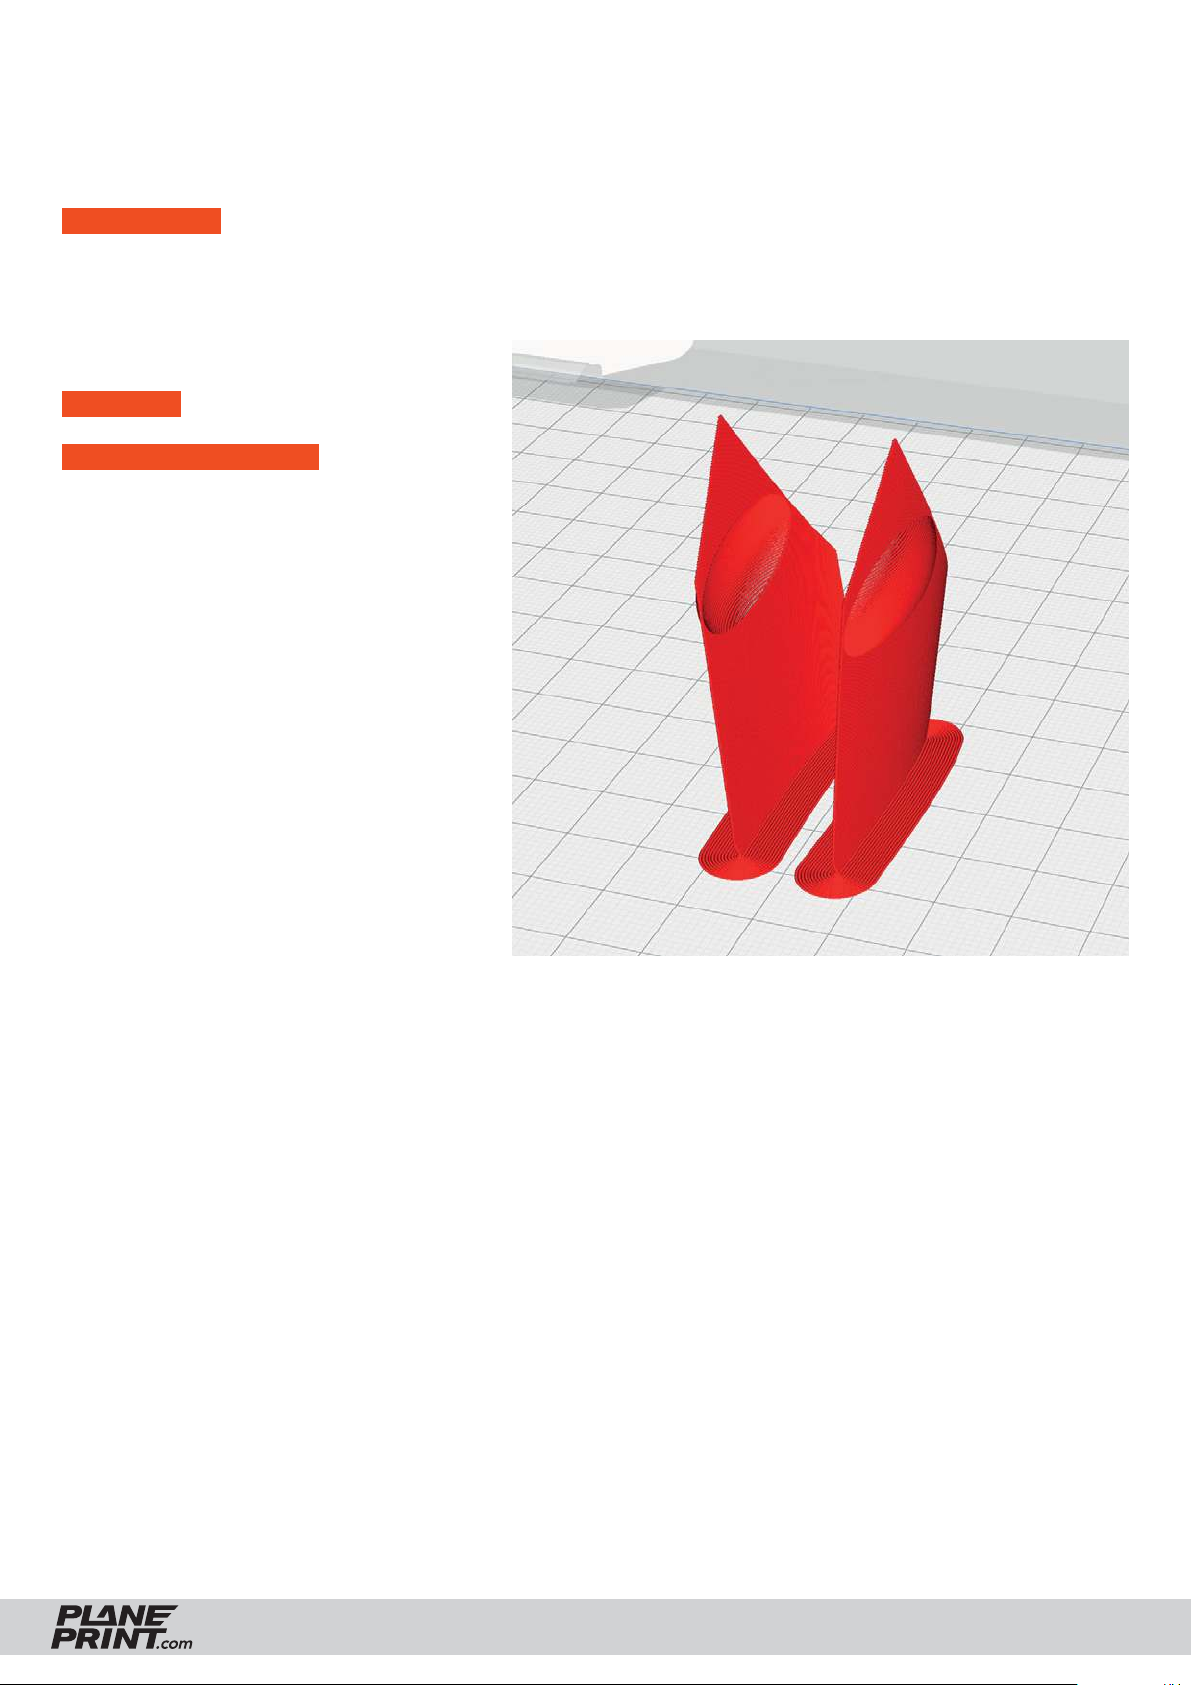
PROFILE P3_SURFACE normal PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Servocovers-profile3.stl
MATERIAL PLA, ~ 2 g
ADDITIONAL SETTINGS
None required
If you have problems with printing, there
is a combined version in the Individual
parts folder.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
9
Page 10
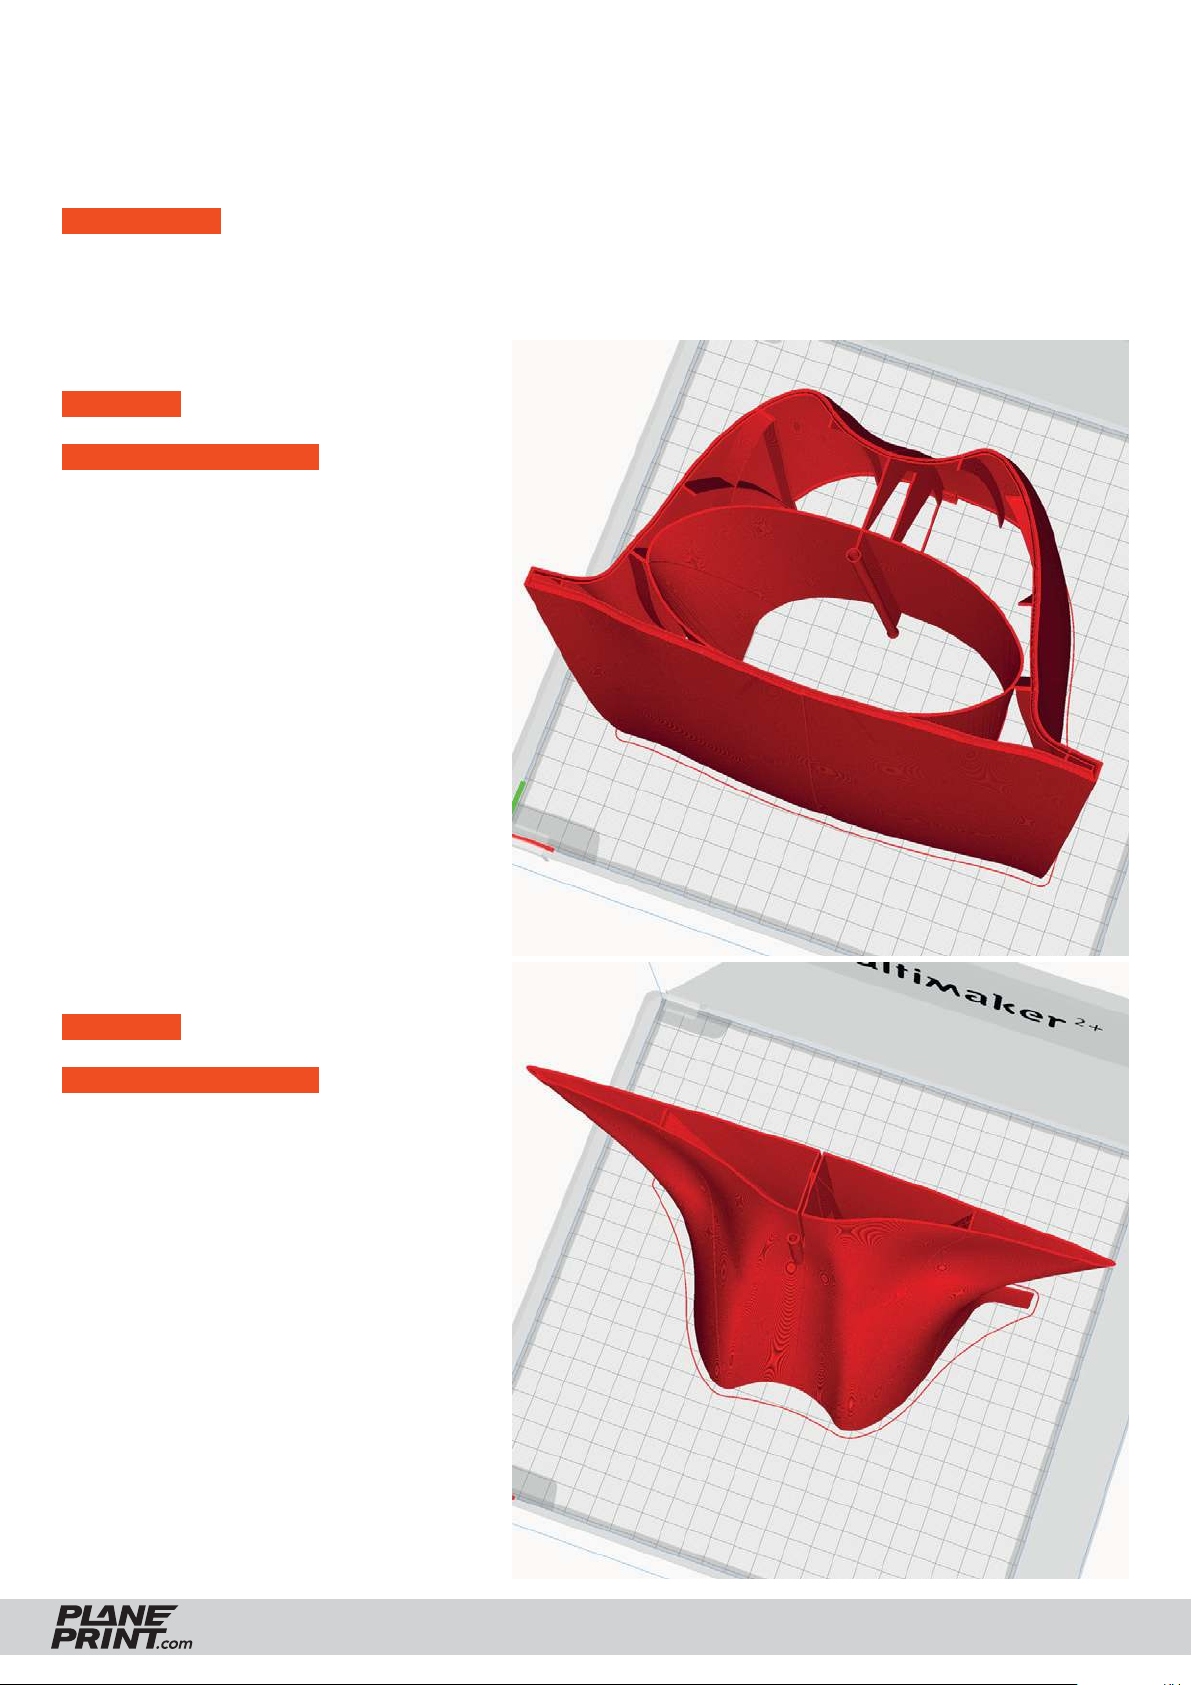
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Body2_LW-profile3.stl
MATERIAL LW-PLA, ~ 105 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
eagle-Body3_LW-profile3.stl
MATERIAL LW-PLA, ~ 38 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
10
Page 11
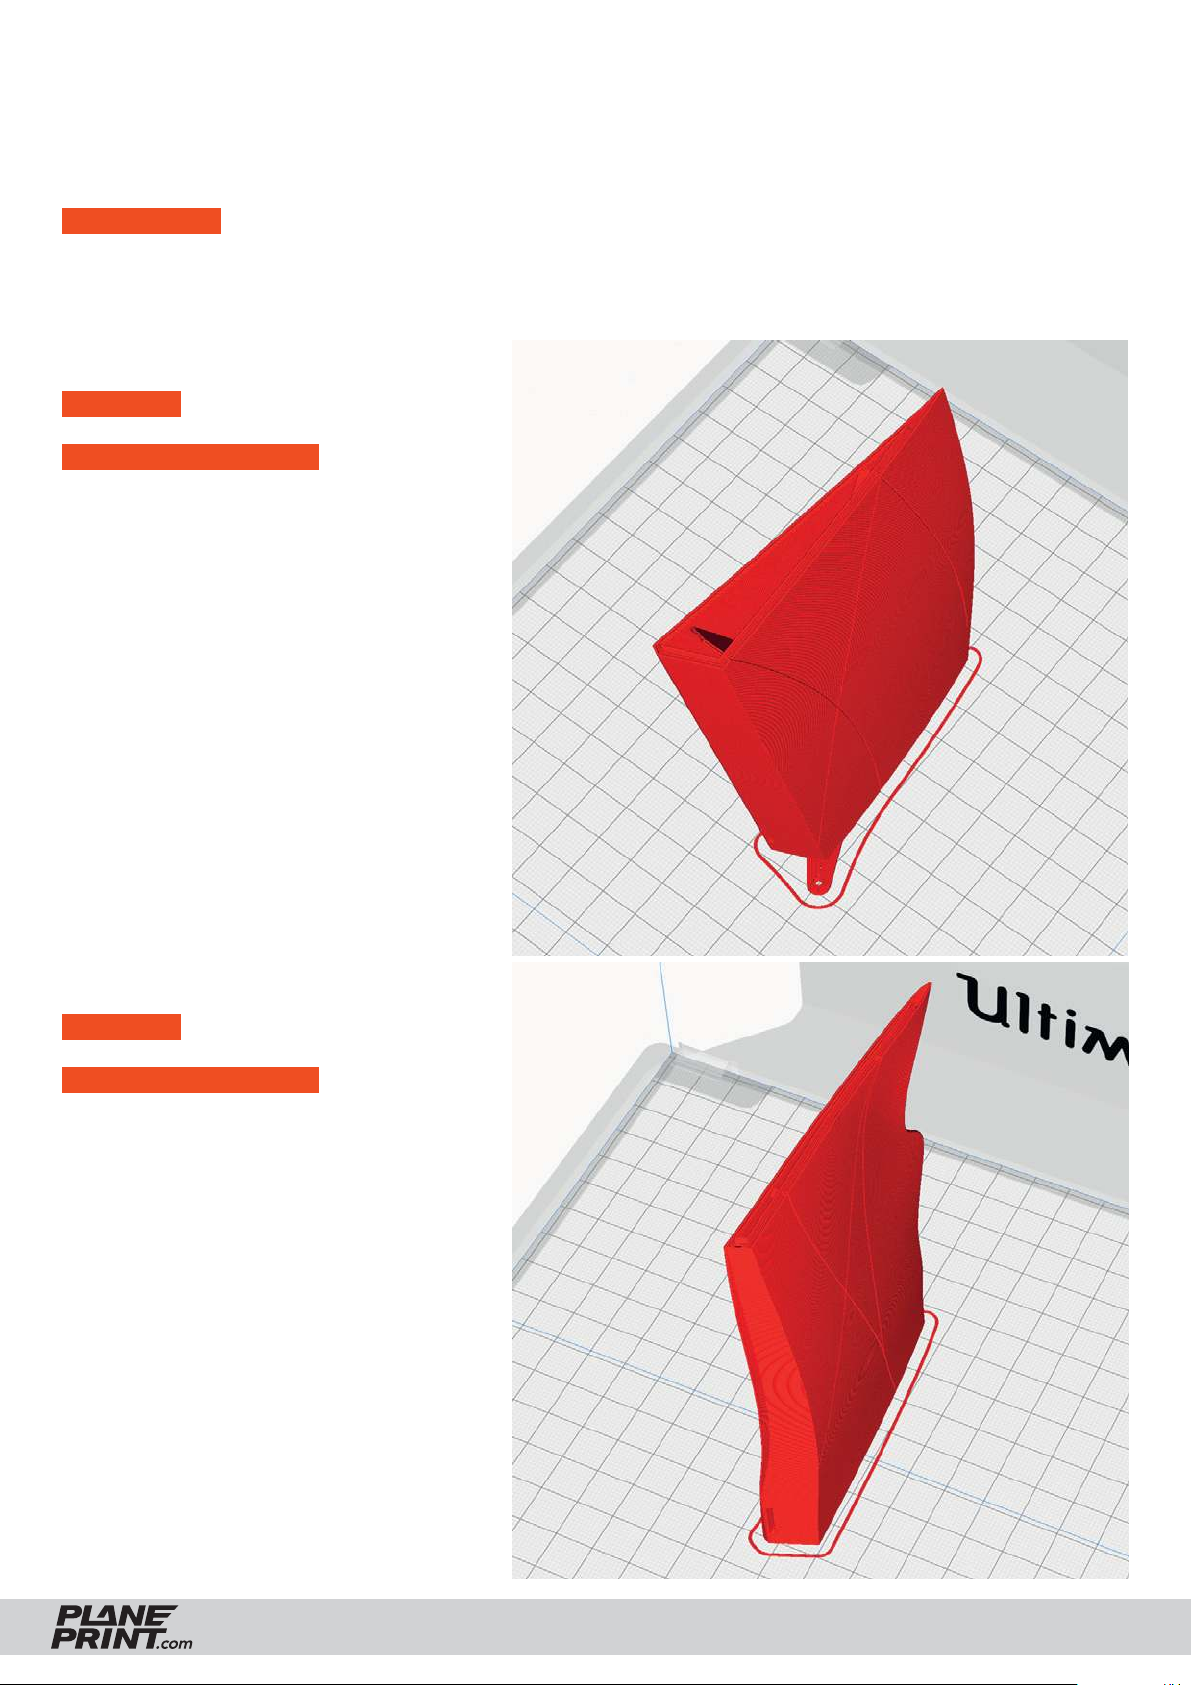
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Aileron1_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 18 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
eagle-Aileron2_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 15 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
11
Page 12
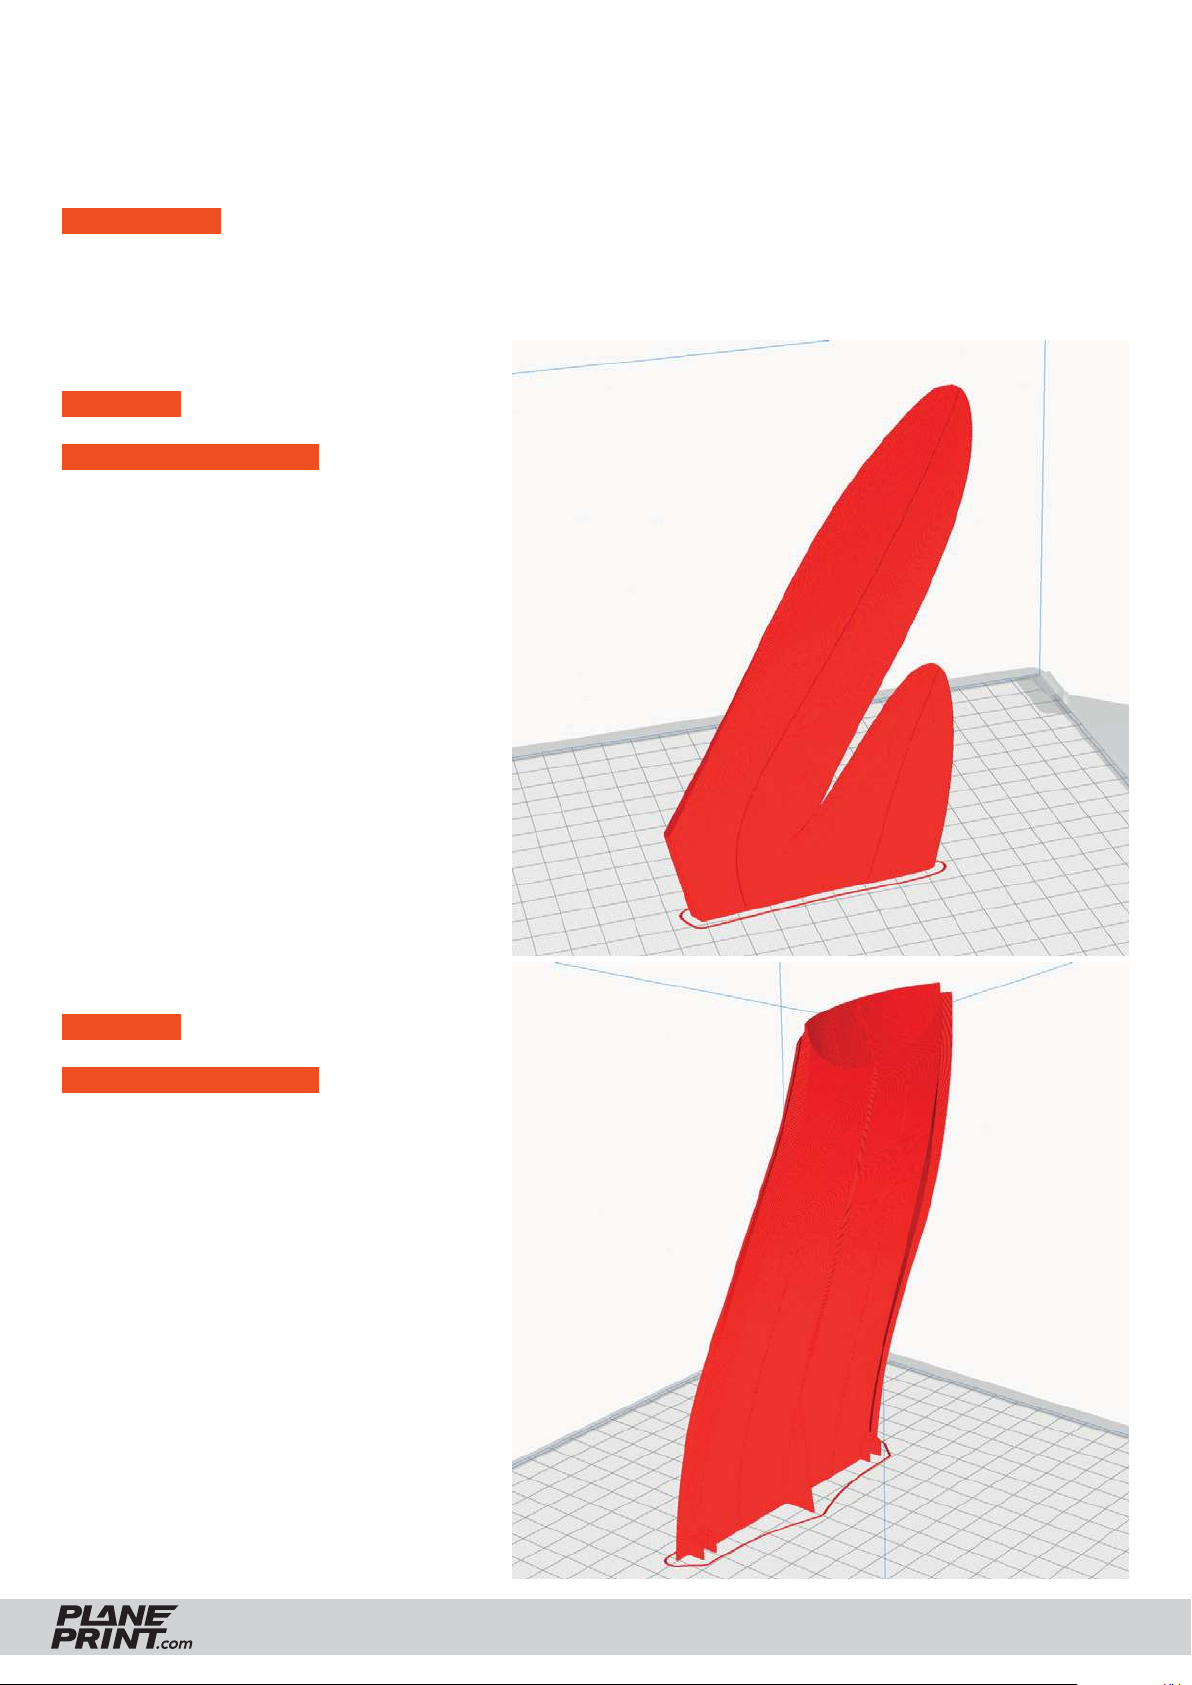
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Aileron3_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 10 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
eagle-Cover_LW-profile3.stl
MATERIAL LW-PLA, ~ 21 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
12
Page 13
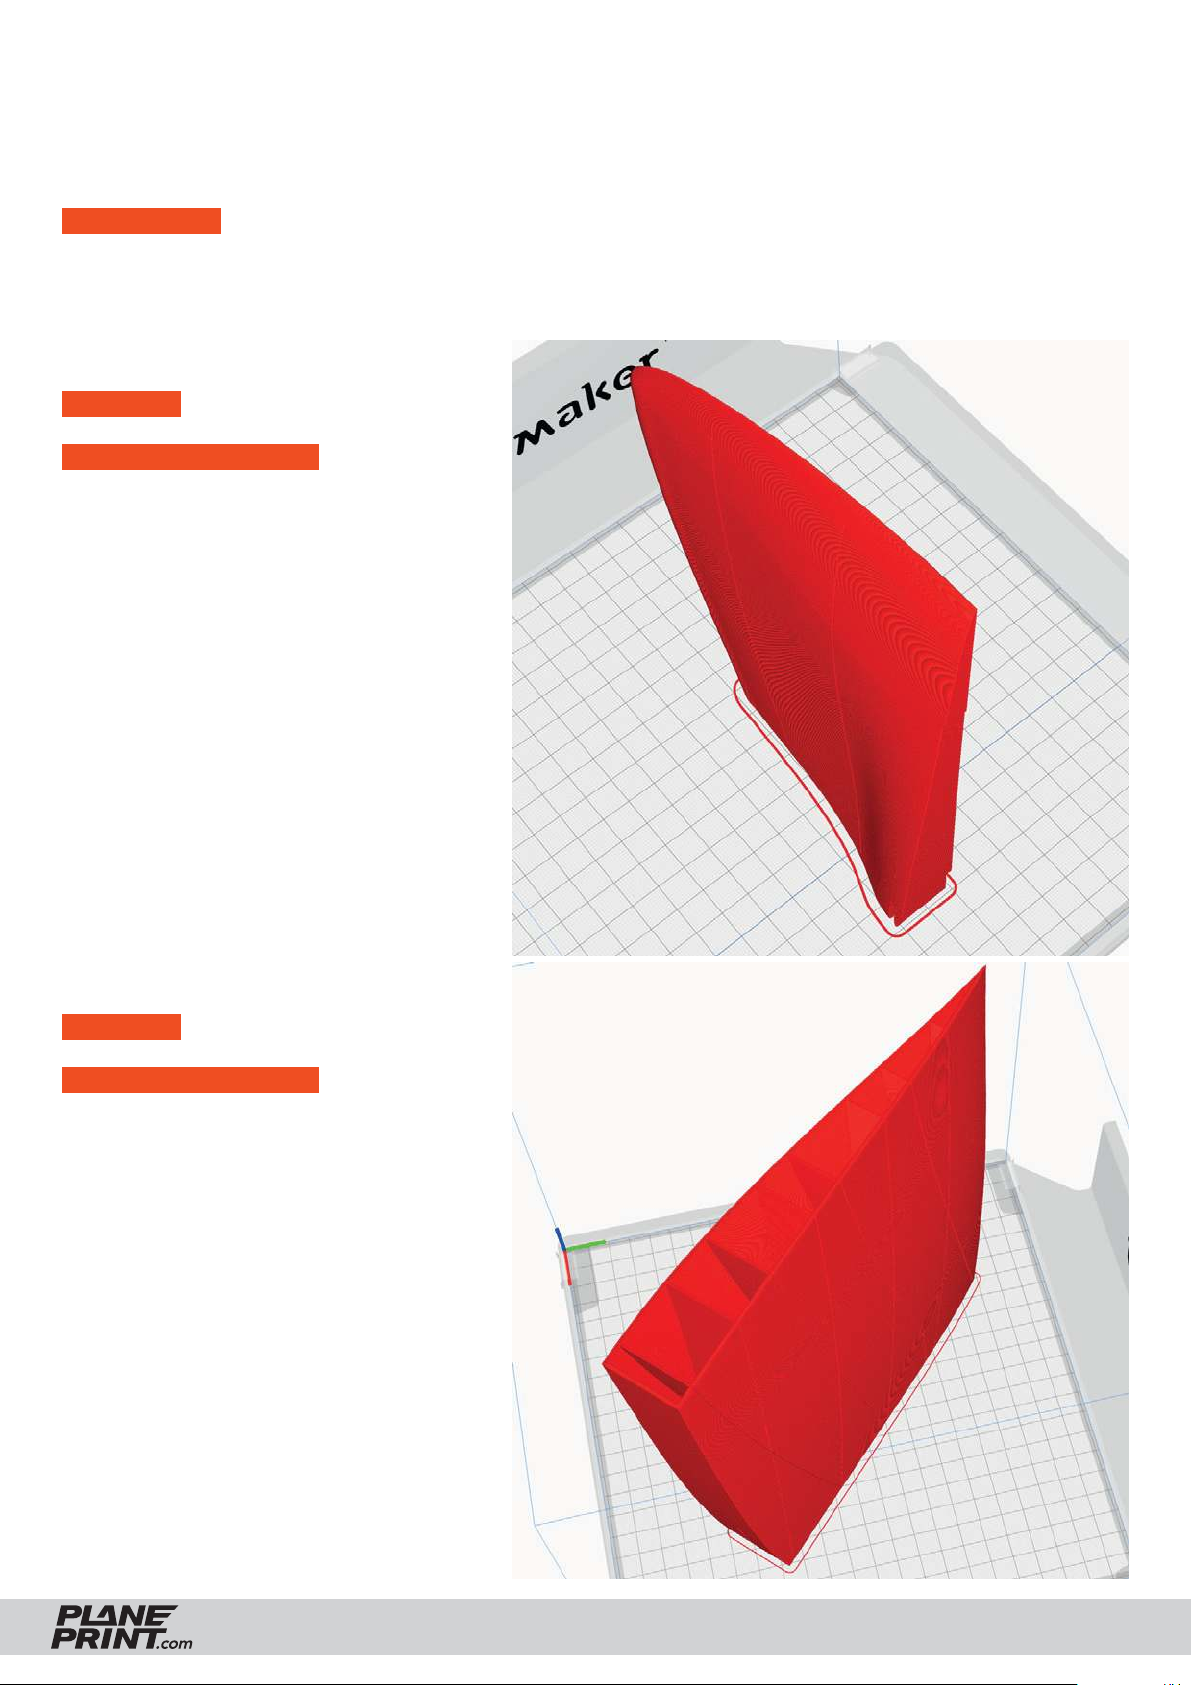
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Tail-left/right_LW-profile3.stl
MATERIAL LW-PLA, ~ 23 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
eagle-Wing4_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 74 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
13
Page 14
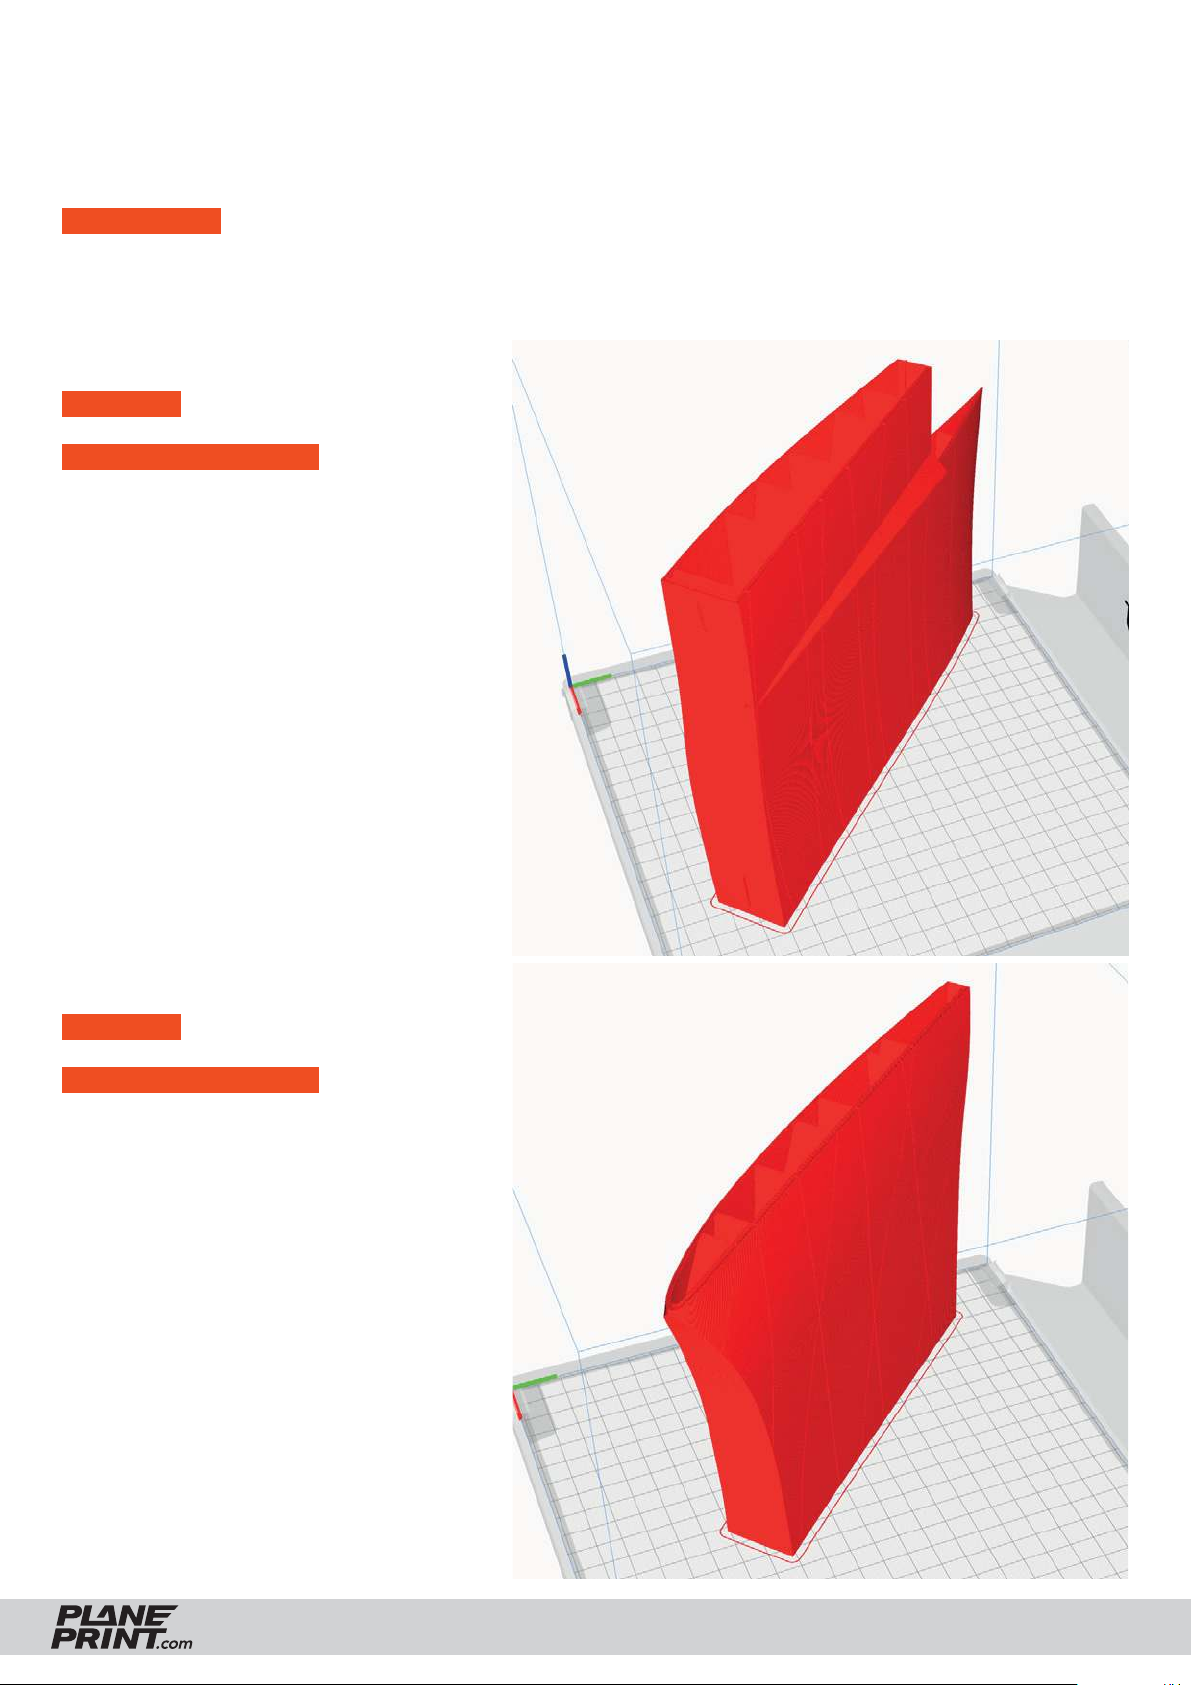
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Wing5_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 78 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
eagle-Wing6_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 63 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
14
Page 15
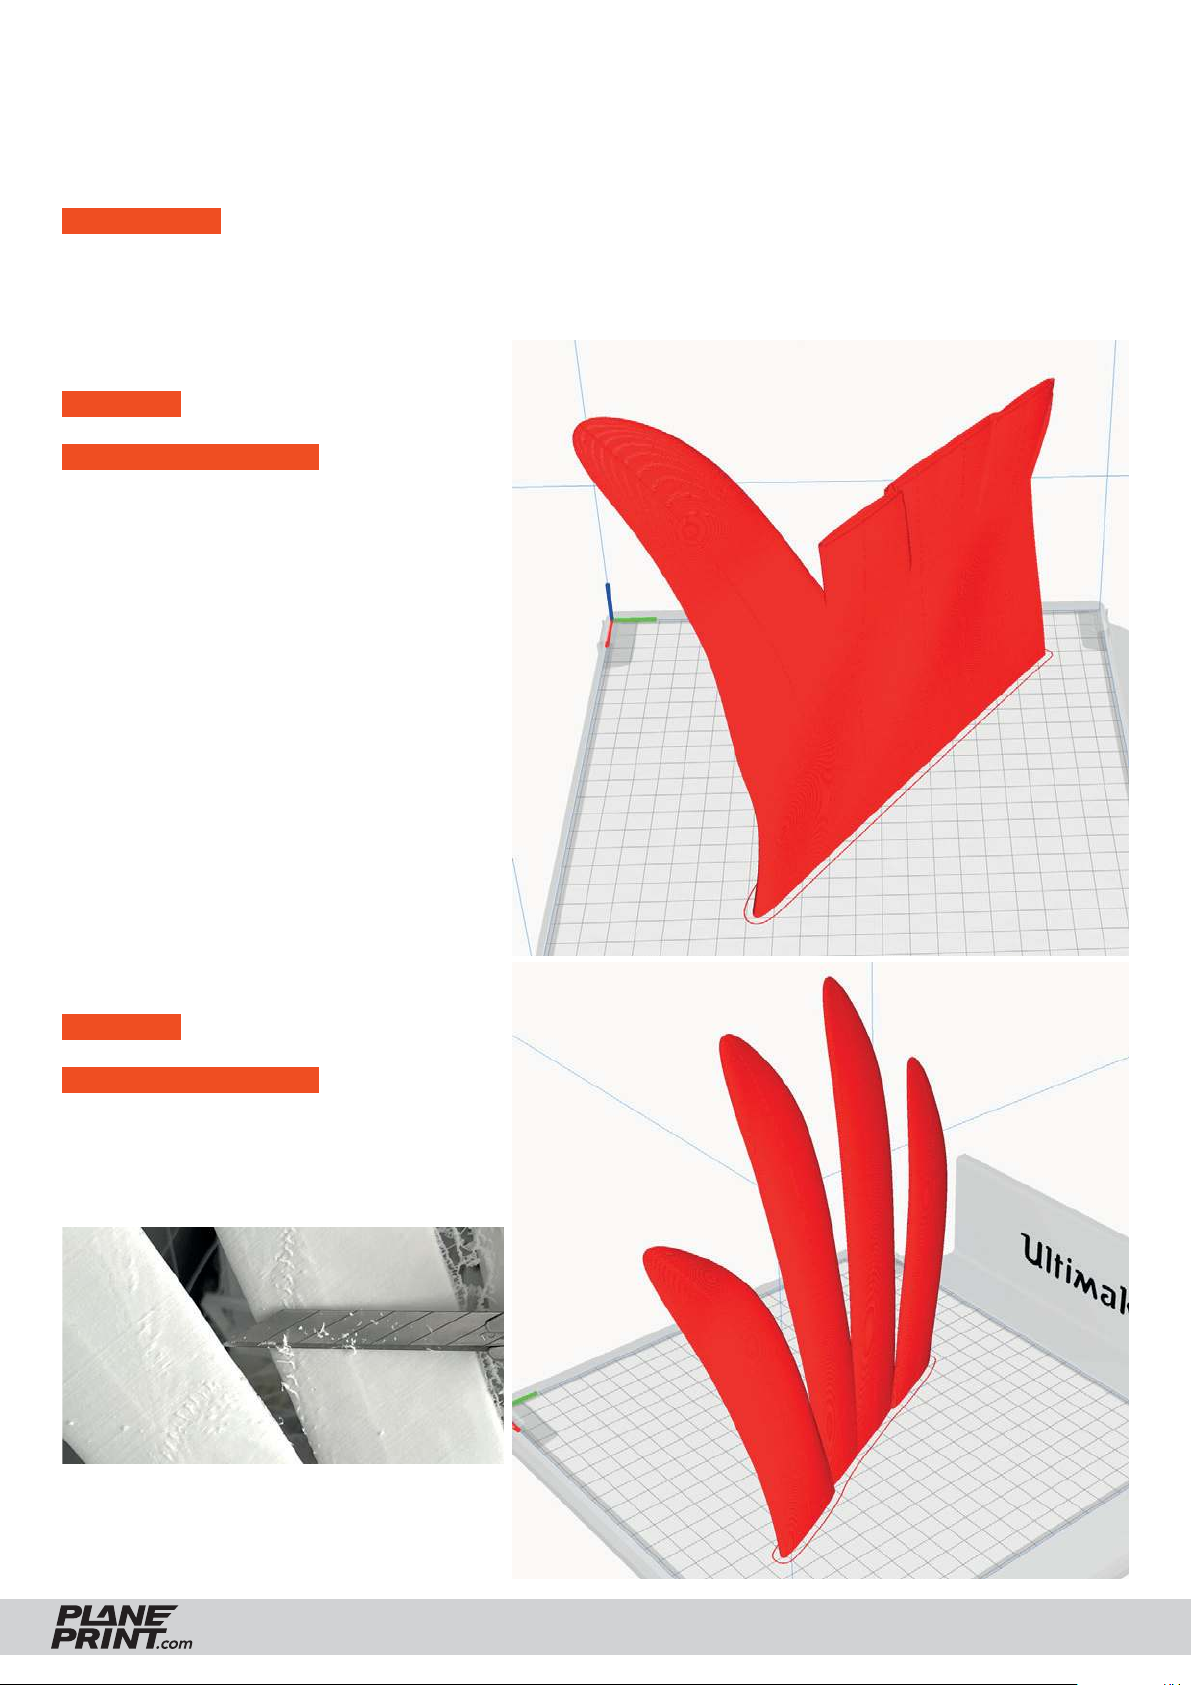
PROFILE P3_SURFACE Light-Weight LW-PLA
The following parts must be sliced with the PROFILE P3_SURFACE (1-wall-print).
Please note the additional settings for the individual parts!
PLEASE NOTE In profile P3_SURFACE, there should not be more than one STL on the buildplate at the same
time, otherwise slicing errors can occur! Depending on your printer, a brim may not be required.
eagle-Wing7_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 37 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
The optimal weight and sufficient strength is achieved
with 60 % flow. Increase the temperature until the wall
thickness is 0.4 to 0.5 mm. (We print at 250° and 60% flow).
*Display in Cura. The actual weight is then 60% of this.
eagle-Wing8_LW-left/right-profile3.stl
MATERIAL LW-PLA, ~ 30 g*
ADDITIONAL SETTINGS
- Setting Profile3_Surface
- Flow 60 %
- Higher nozzle temperature
LW PLA
Since stringing is unfortunately unavoidable when
printing LW-PLA, this part have to be cleaned up
with the cutter.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
15
Page 16
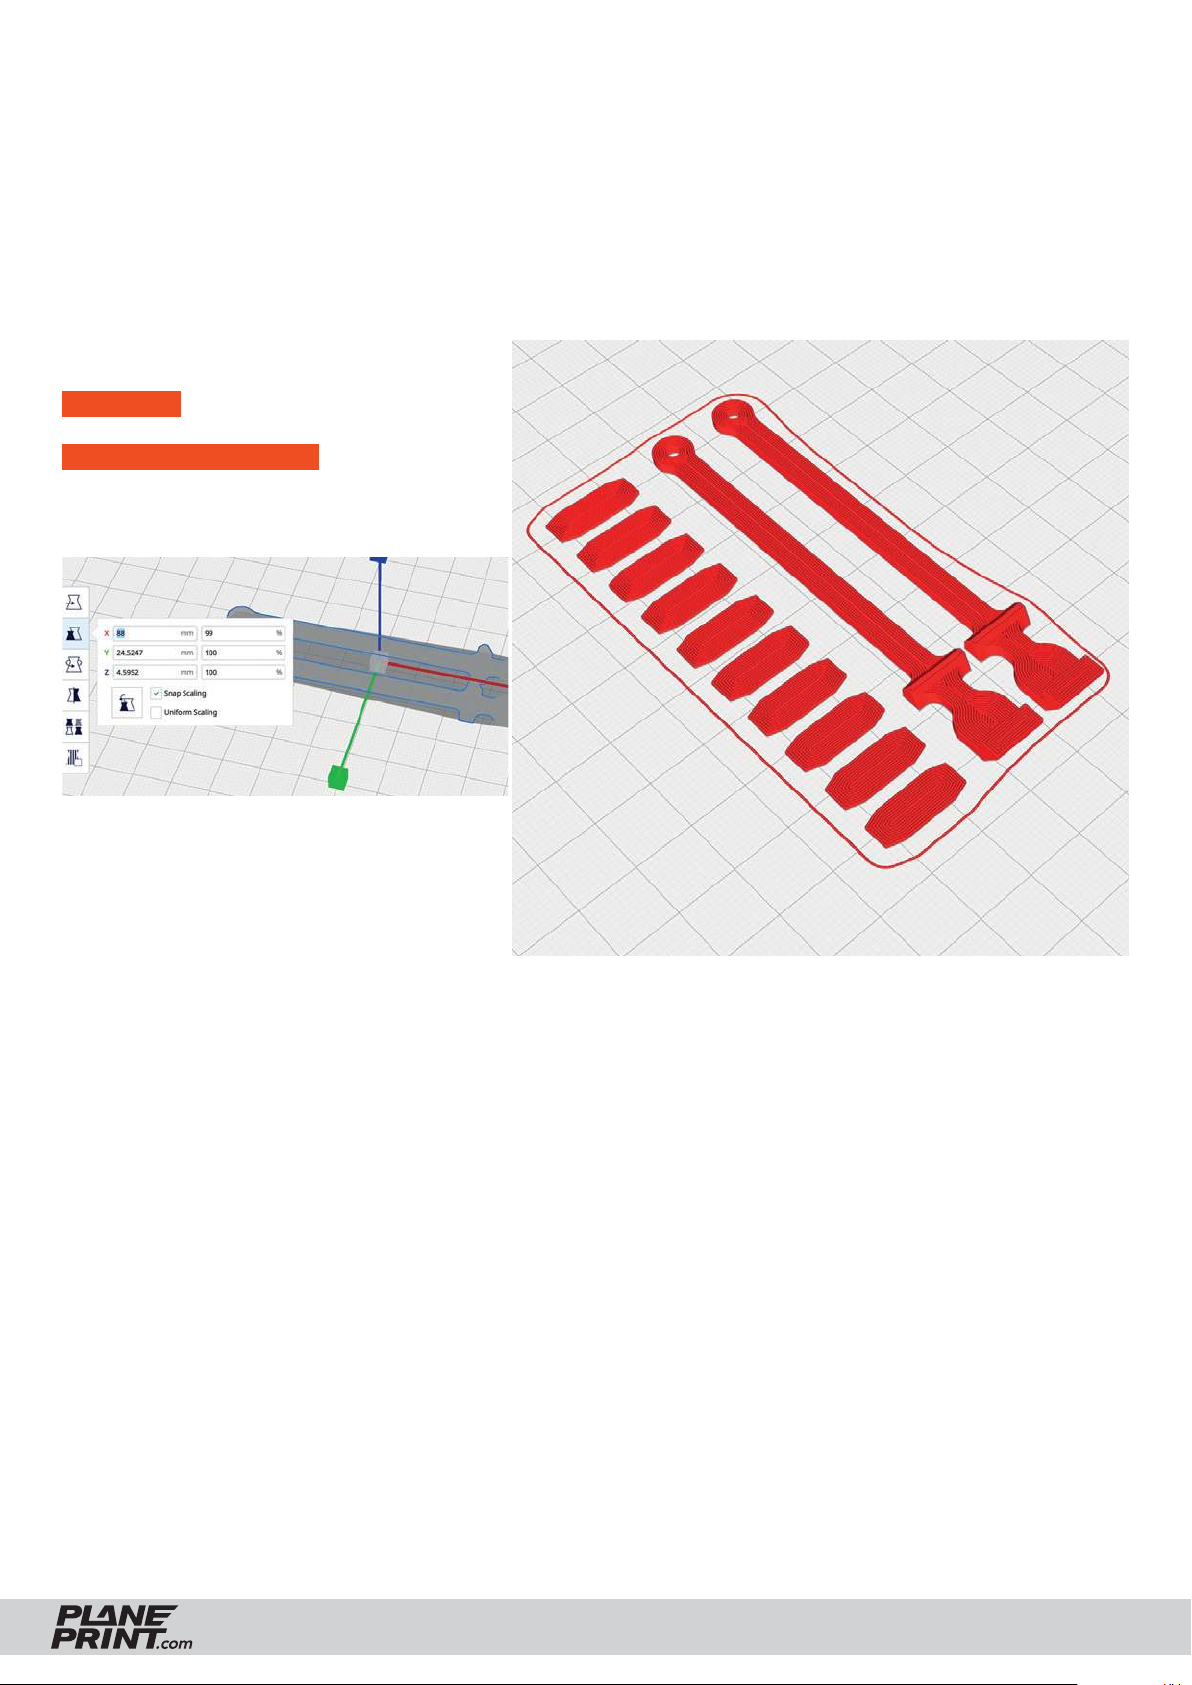
PROFILE P4_FLEX
The following parts must be sliced with the PROFILE P4_FLEX.
Please note the additional settings for the individual parts!
eagle-Parts-flex-profile4.stl
MATERIAL TPU ~ A95, Weight: ~ 4 g
ADDITIONAL SETTINGS
• Wall Line Count: 10
Tension belt lenght
In the folder Individual parts you will find the tension
belts also as a single file. If you want to change them
slightly in length, you can simply change the dimension of the X-axis in Cura (Uniform scaling must NOT
be selected).
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
16
Page 17
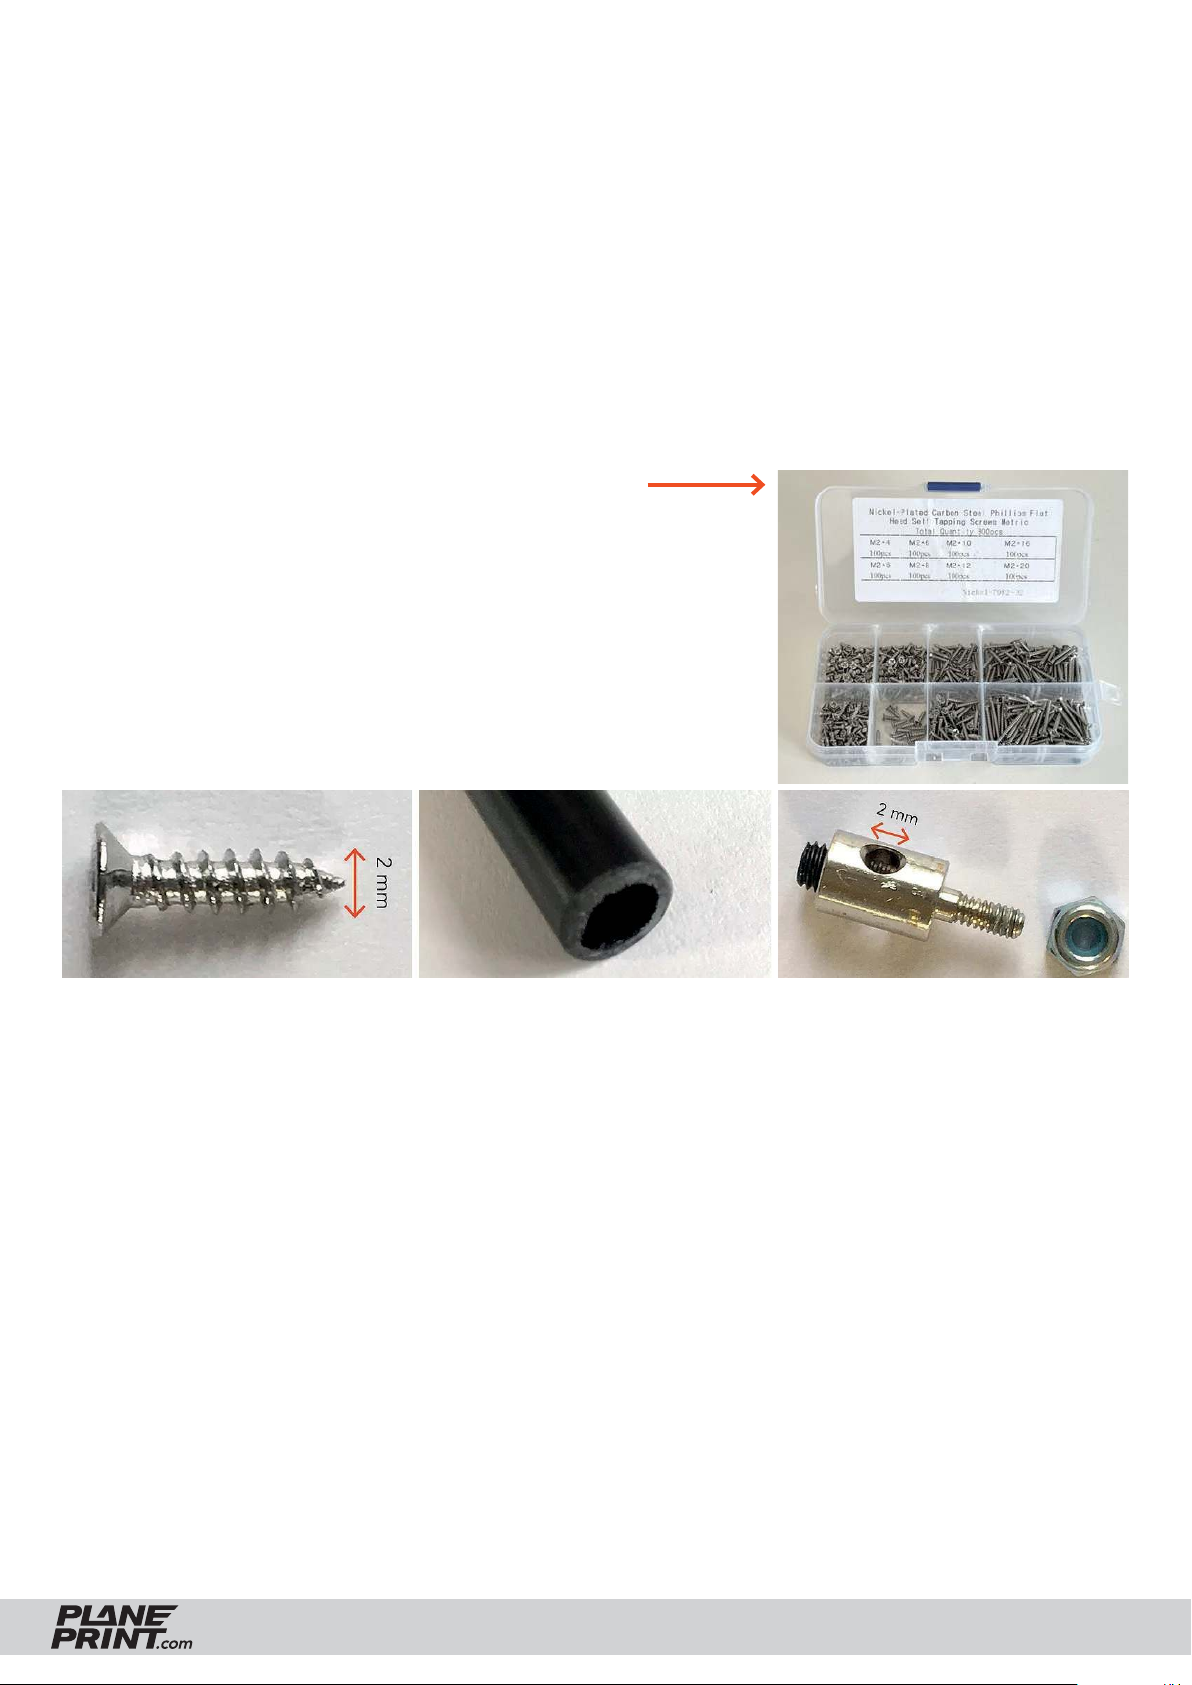
REQUIRED ACCESSOIRES
Filament
• normal PLA about 400 grams
• LW-PLA about 500 grams
• TPU (A95) about 10 grams
(Absolutely necessary)
Materials
• some tapping screws Ø2*8 mm
(simply search for: M2 flat head tapping screw assortment)
• CA super glue (liquid and liquid medium)
• CA activator
• Servo extension cable 300mm, 2 pieces
• Carbon tube Ø8*1000mm, 1 piece
• Steel wire Ø1mm
• Neodym-Super-Magnet 5*5*5mm, 4 pieces
• Rod connection, 3 pieces
• Foil 0,5mm/0.020inches Din A4 (PVC, PET-G, Polycarbonate or Lexan),
1 piece
Tools
• Cutter knife
• small Philips screwdriver
• Drill Ø2,5mm, Ø1,5mm
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
17
Page 18
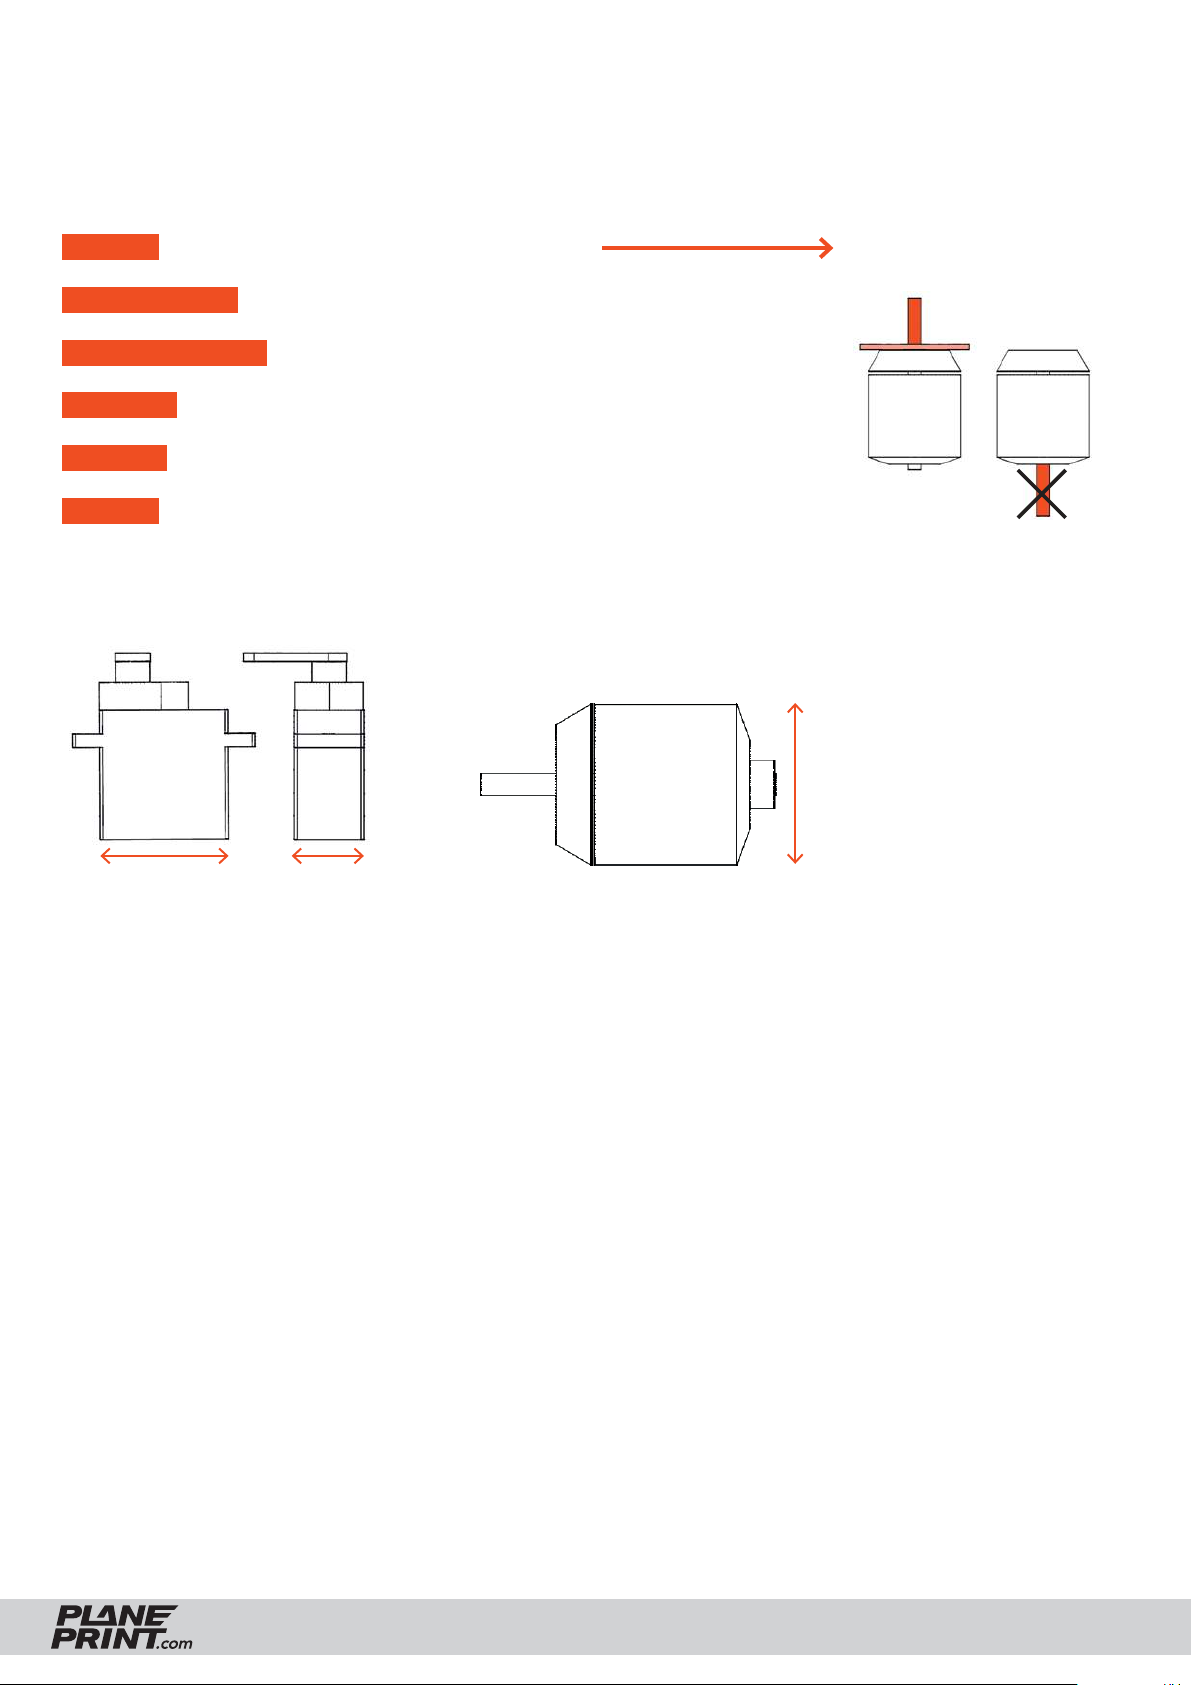
RC Components
The Notos allows the installation of a wide variety of drives.
We have good experience with this version:
ENGINE RAY G3 C2836/1120 or comparable motors
FOLDING PROP 11x5 (2S), 10x5 (3S)
BEC-CONTROLLER 30-50 A (must fi t the engine!)
RECEIVER 4 Channel
BATTERY 2S or 3S Lipo, about 1000-2200 MaH
SERVOS Hitec HS-55 or EMAX ES08(A or D), 3 pieces
Pay attention to the position
of the motor shaft
(1.1 inches)
Ø max. 28 mm
max. 22,5 mm
(0.88 inches)
max. 12 mm
(0.47 inches)
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
18
Page 19
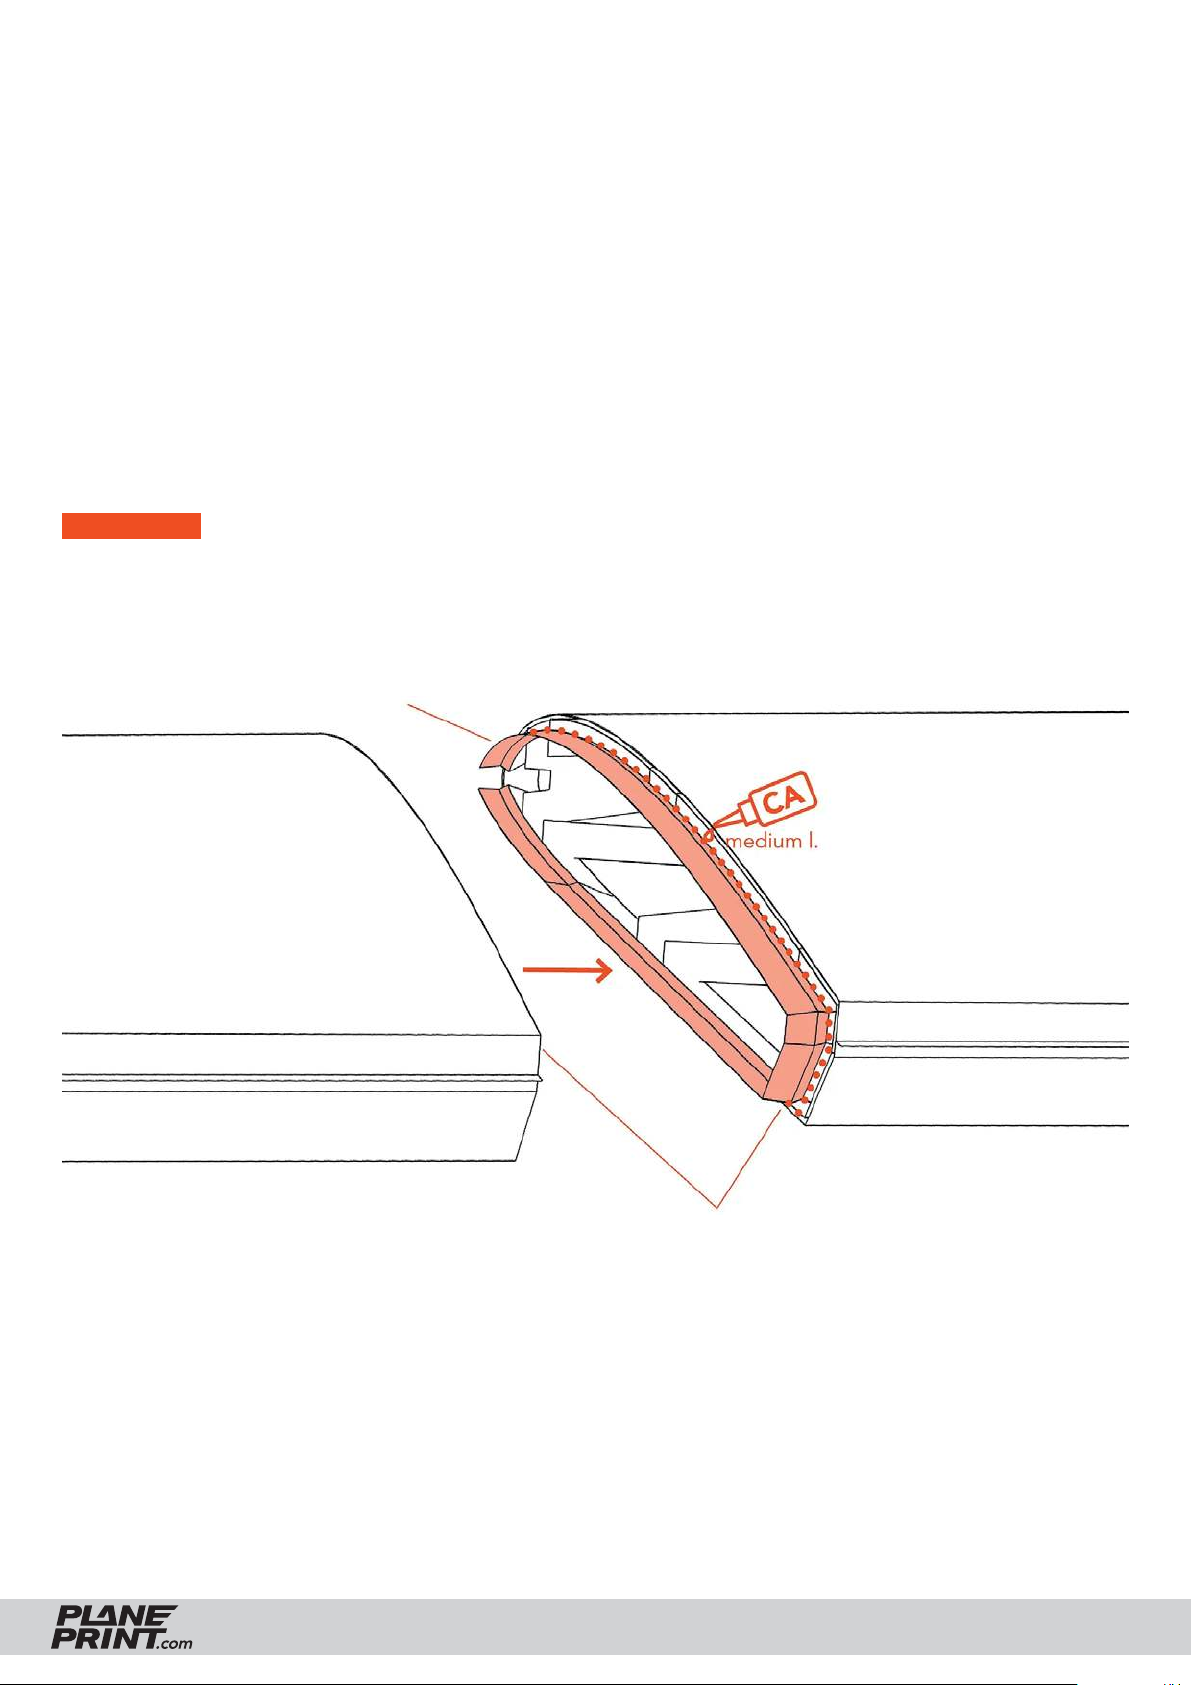
ASSEMBLING MANUAL
Basic information
Gluing the parts
To glue the fuselage and wing parts well, use medium-liquid CA adhesive.
First check whether the parts go well together. Then apply a lot of CA glue to the part with the connections
and all surfaces that will touch later (except the bowden tubes). Put the parts together and align the parts perfectly. If glue comes out, wipe with a cloth. Then spray activator spray on the glue points.
IMPORTANT For a strong connection, the adhesive surfaces should be sanded. Please only use fresh CA
glue and activator spray for curing! The adhesive connections must hold perfectly!
Connection pieces
This surfaces should be sanded
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
19
Page 20
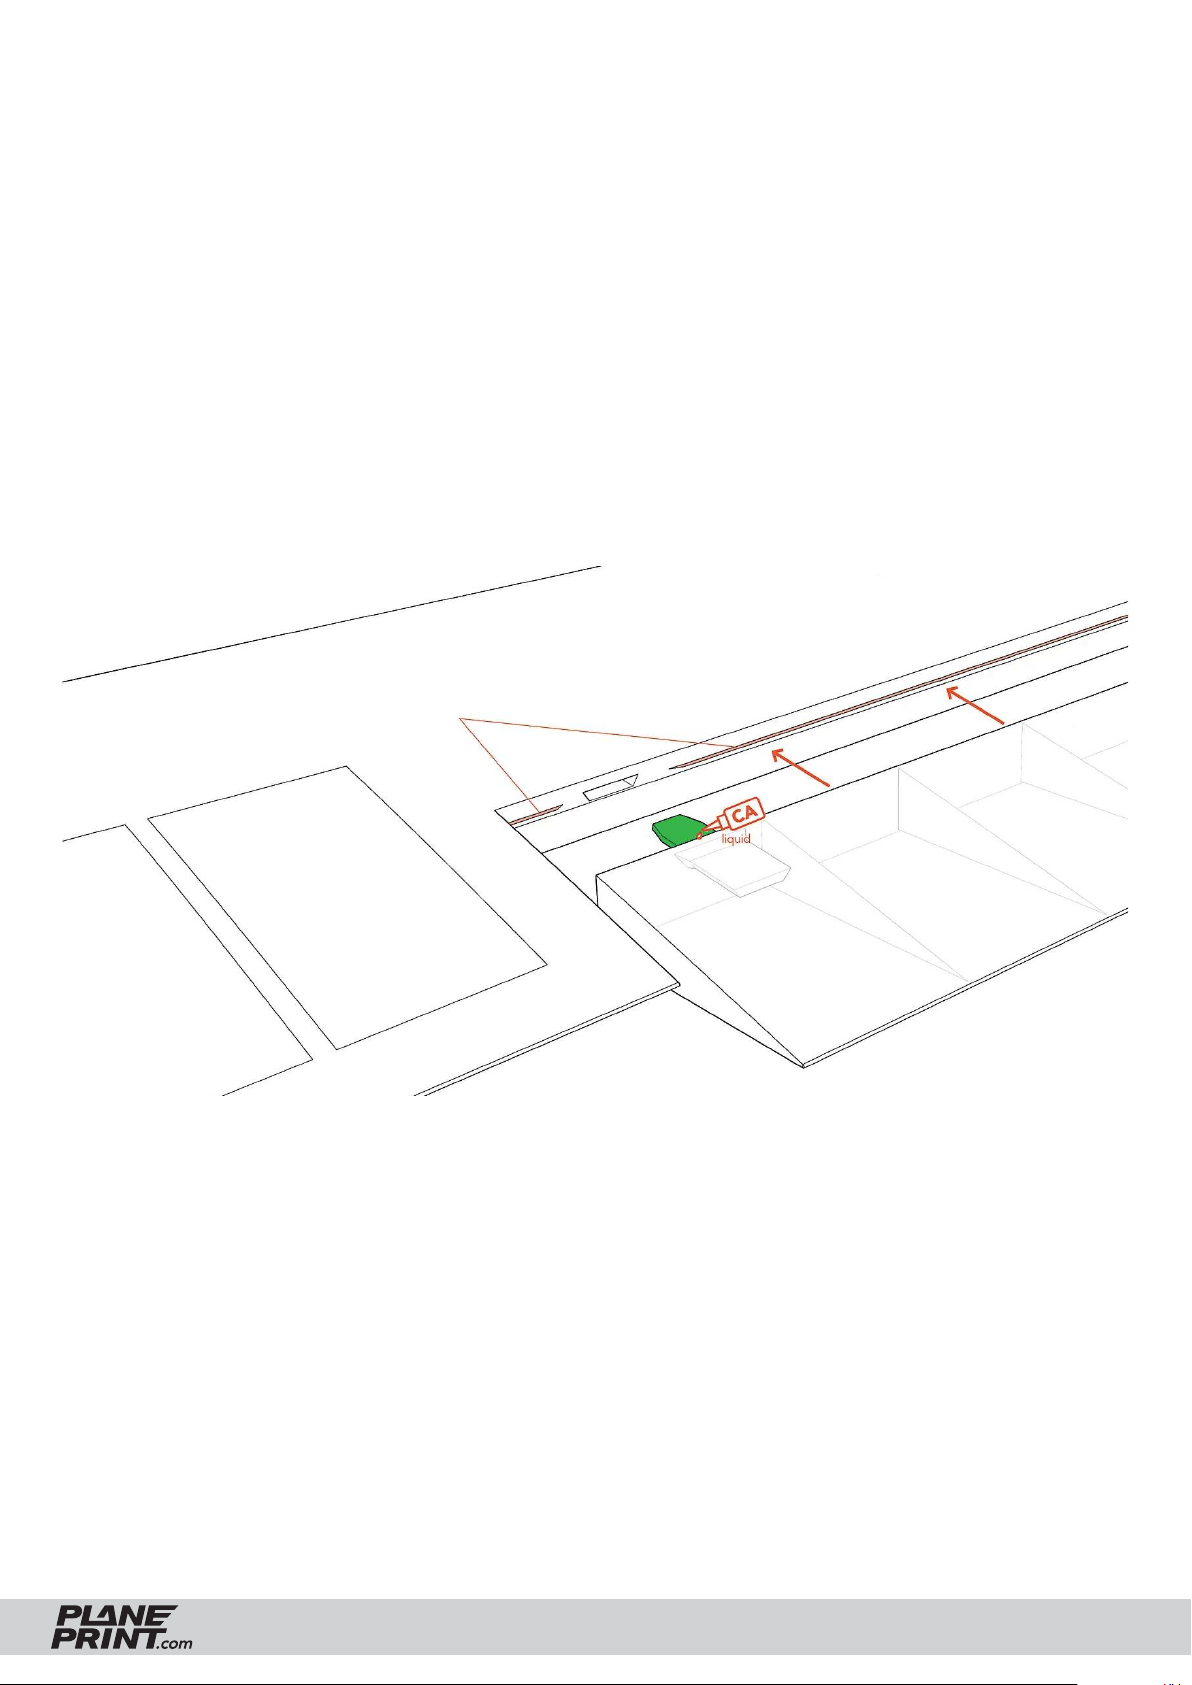
Basic information
Installation of the TPU hinges
First insert the hinge into the movable flap and add a drop of liquid CA adhesive into the gap.
Wait for the glue to drain completely, then spray the activator on it.
Then put the flap in the wing until the flap touches the spacers and put a drop of CA glue on the hinge.
Wait again for the glue to run in, and then spray the activator on it.
Do not use too much glue, the flap must move easily!
These spacers ensure the correct
gap distance. Don´t remove!
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
20
Page 21
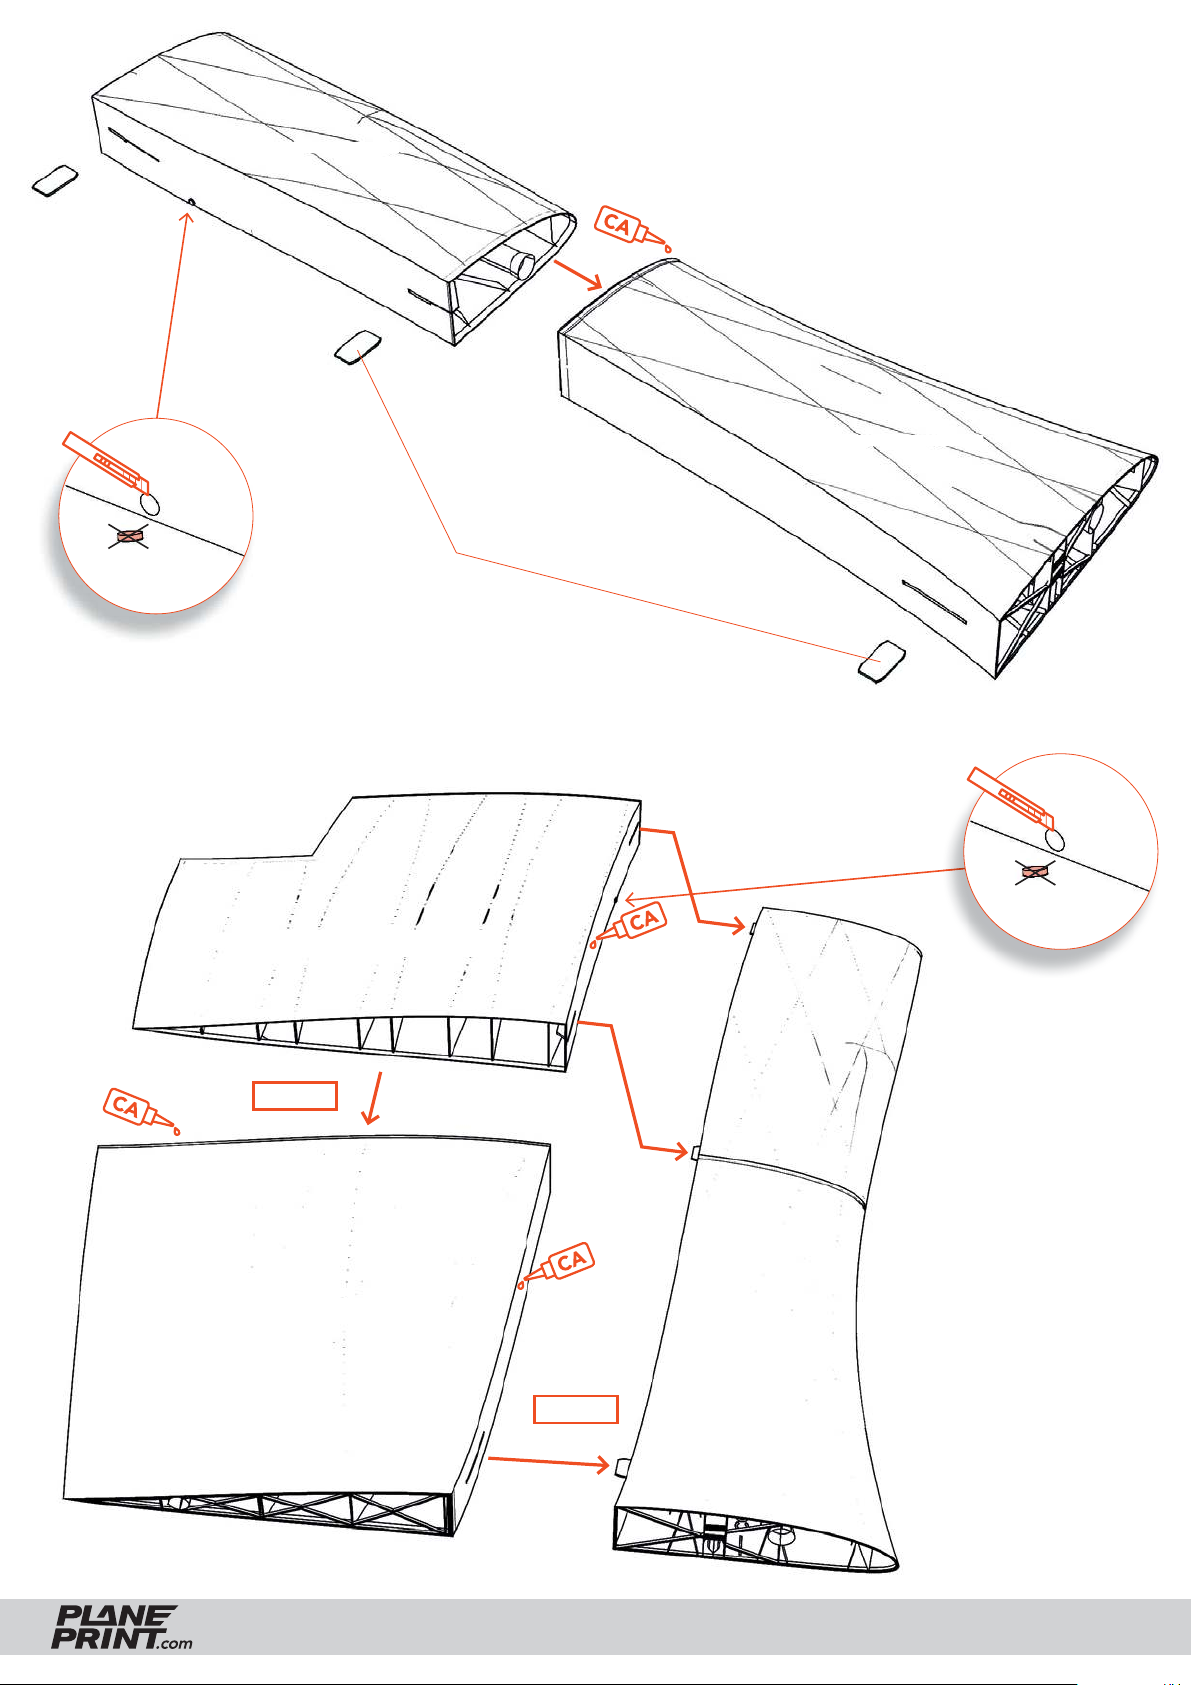
remove support
Wings assembly 1
eagle-Wing2-left-profi le3.stl
medium l.
eagle-Wing1-left-profi le3.stl
eagle-Parts-profi le1.stl
Wings assembly 2
eagle-Wing5_LW-left-profi le3.stl
STEP 1
medium l.
eagle-Wing4_LW-left-profi le3.stl
medium l.
medium l.
EAGLE
STEP 2
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
21
Page 22
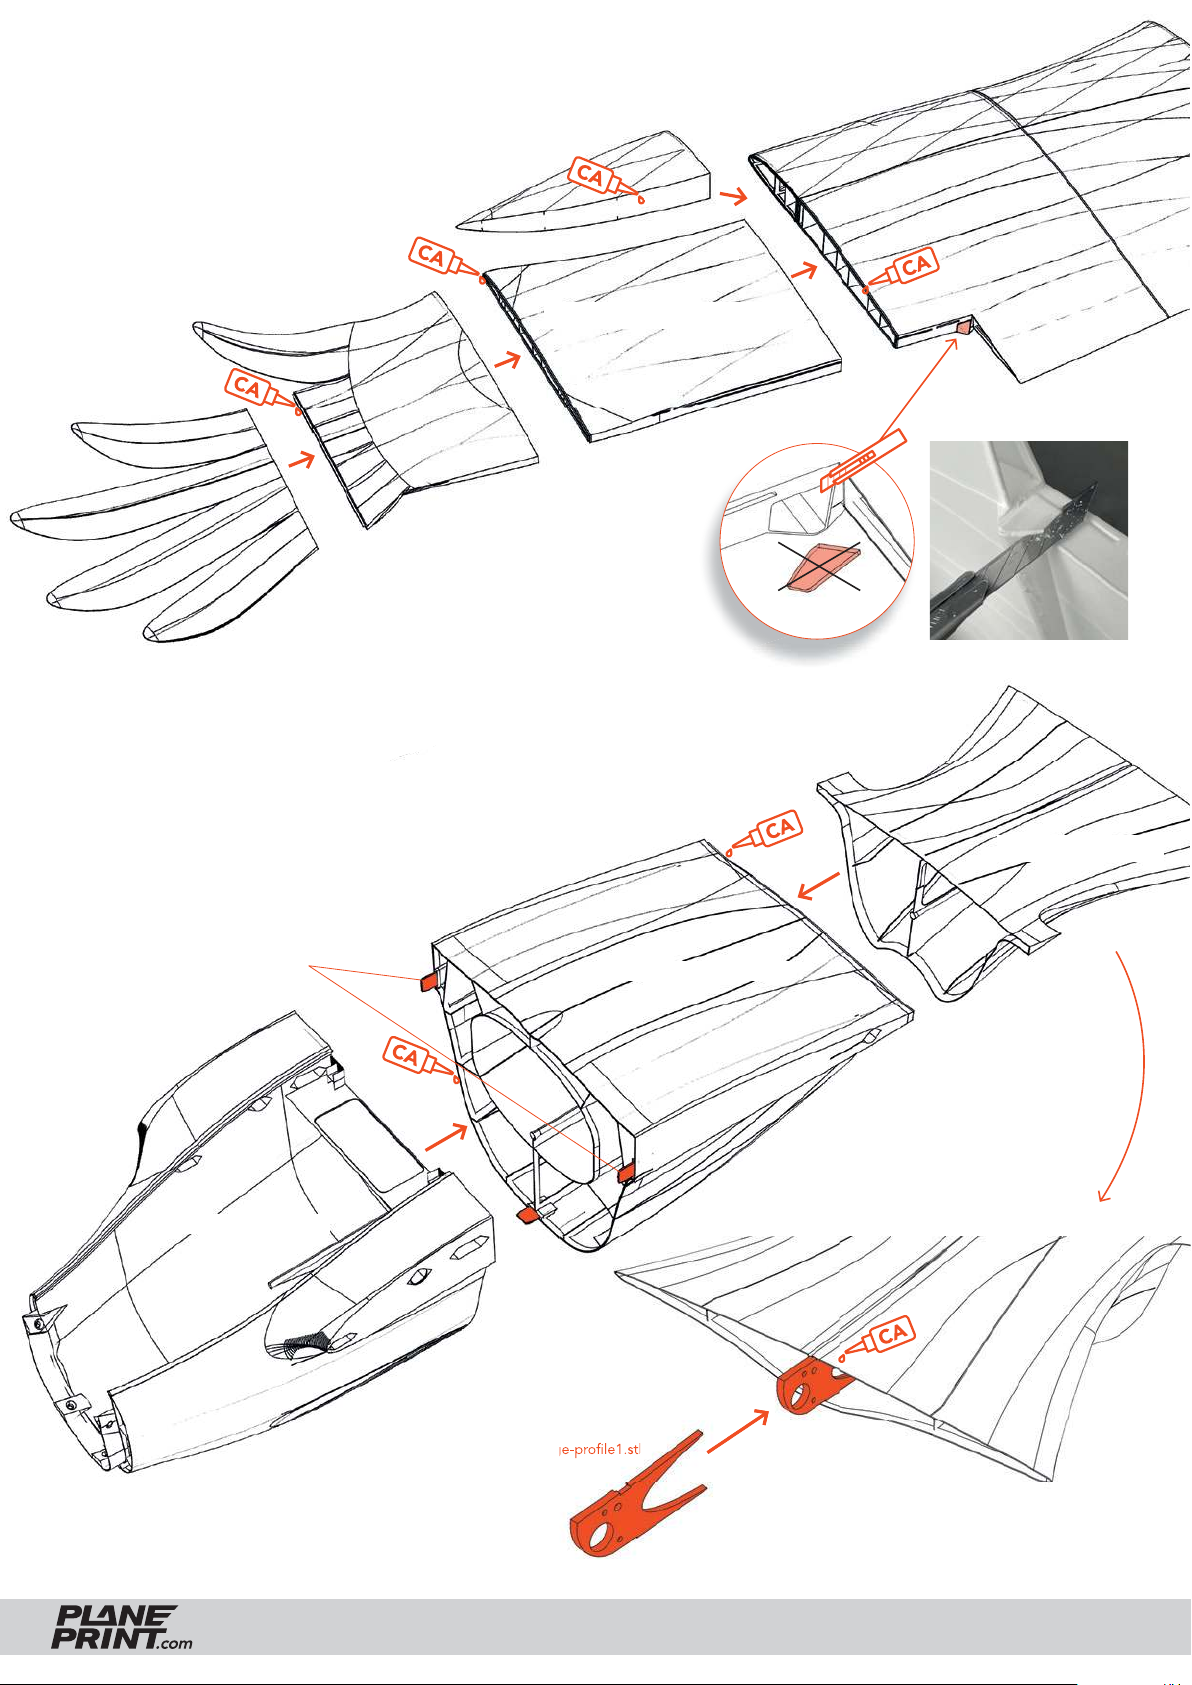
Wings assembly 3
medium l.
medium l.
medium l.
eagle-Wing7_LW-left-profi le3.stl
eagle-Wing8_LW-left-profi le3.stl
Fuselage assembly
eagle-Wing6_LW-left-profi le3.stl
remove
support
medium l.
medium l.
eagle-Body1-profi le3.stl
eagle-Parts-profi le1.stl
eagle-Body1-profi le3.stl
eagle-Body3_LW-profi le3.stl
medium l.
medium l.
eagle-Tail hinge-profi le1.stleagle-Tail hinge-profi le1.stl
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
22
Page 23
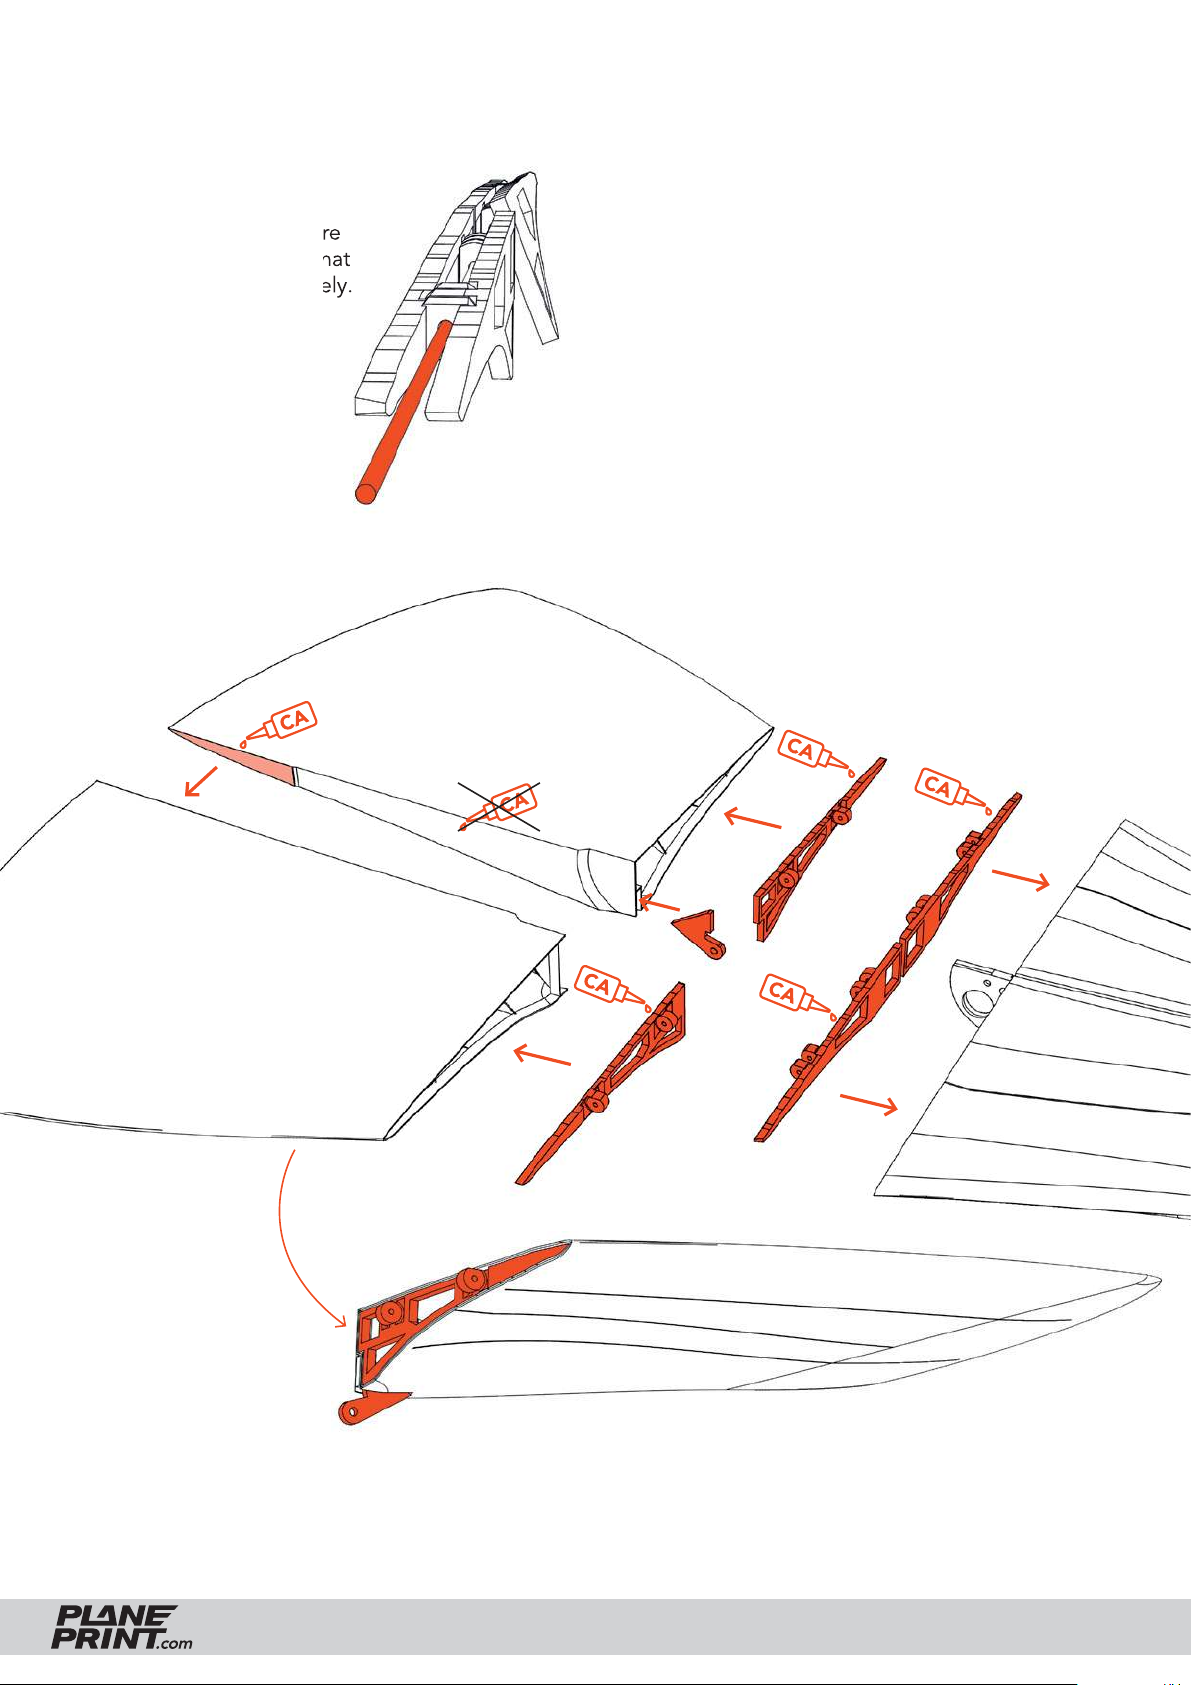
Tailplane assembly
First check that the steel wire
fi ts into the tail hinge and that
it moves easily and accurately.
Steel wire Ø1mm
– step 1
eagle-Tail hinge-profi le1.stl
medium l.
eagle-Tail-right_LW-profi le3.stl
eagle-Tail-left_LW-profi le3.stl
medium l.
eagle-Tail hinge-profi le1.stl
medium l.
medium l.
medium l.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
23
Page 24
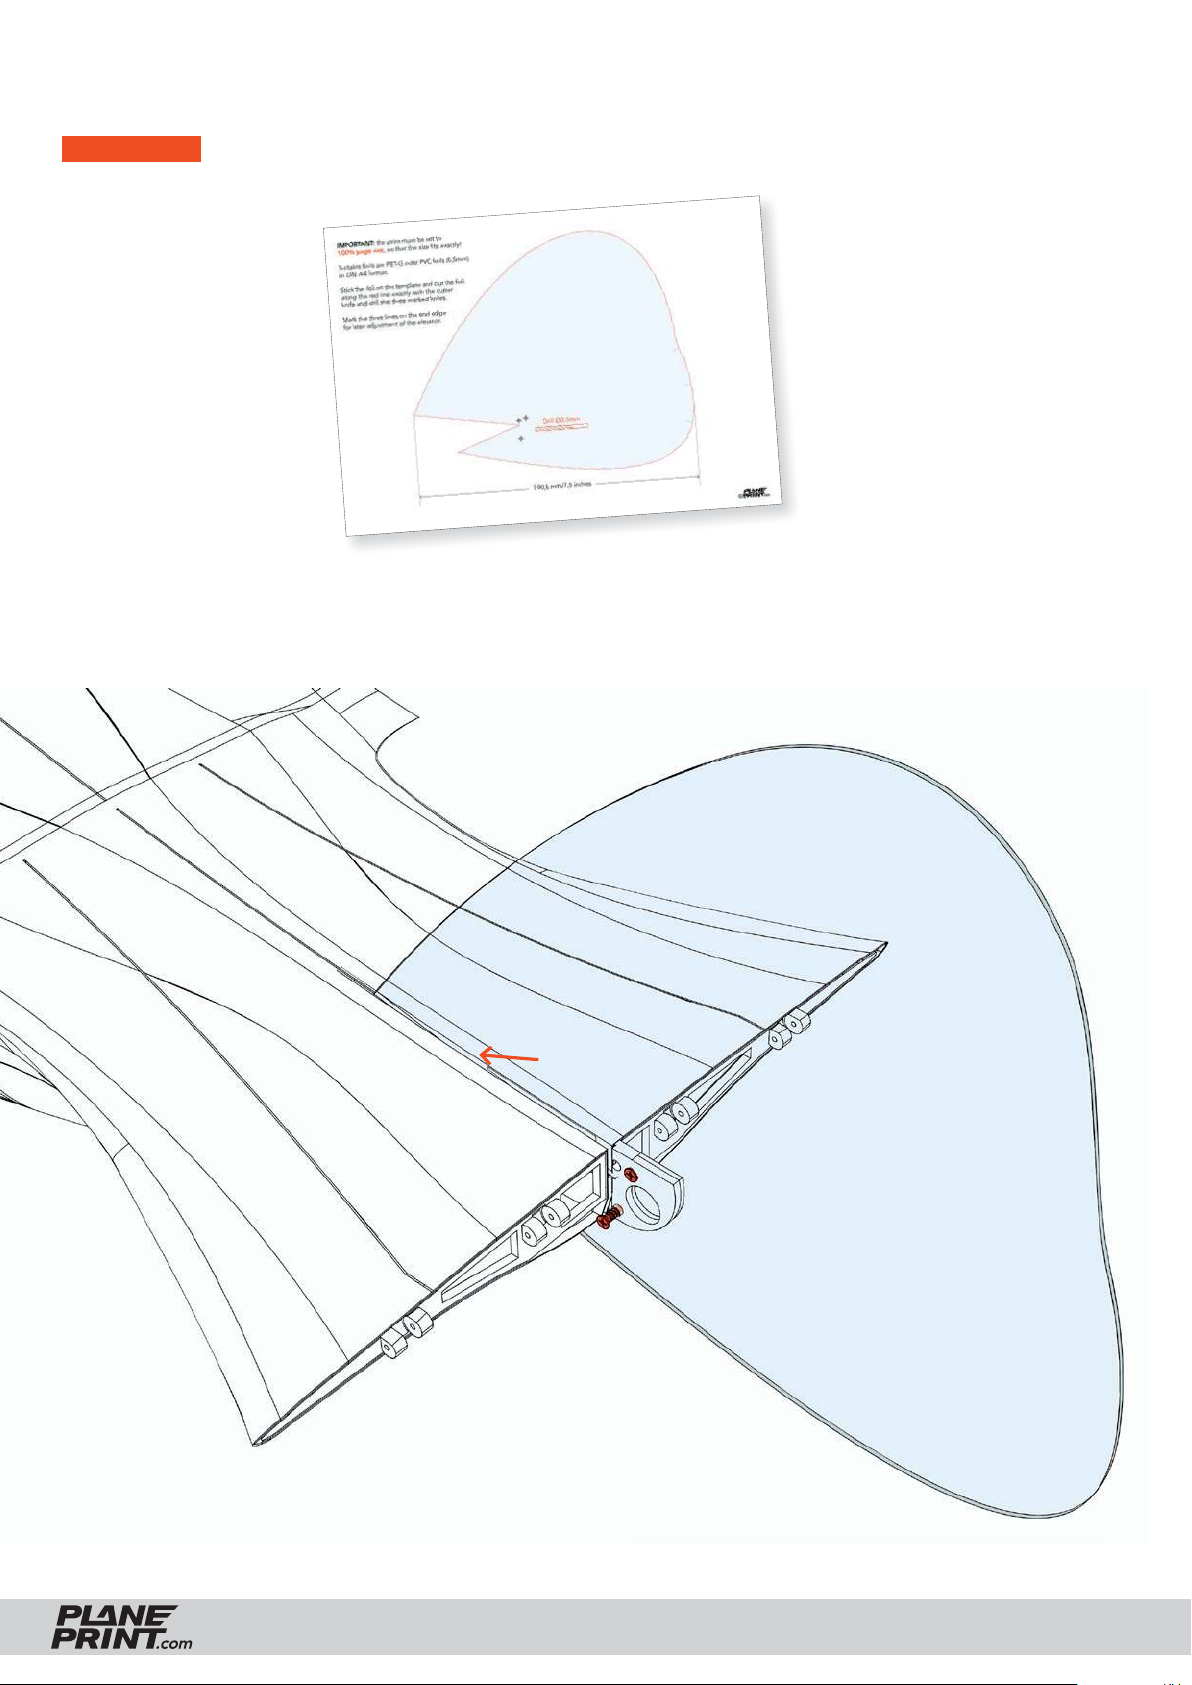
Tailplane assembly – step 1
IMPORTANT The rudder is enormously important for a safe fl ight and must not be smaller!
First, please print the fi le
Rudder template.pdf
from the download folder.
Insert the rudder into the slot of the fuselage
and tighten it with two short tapping screws.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
24
Page 25
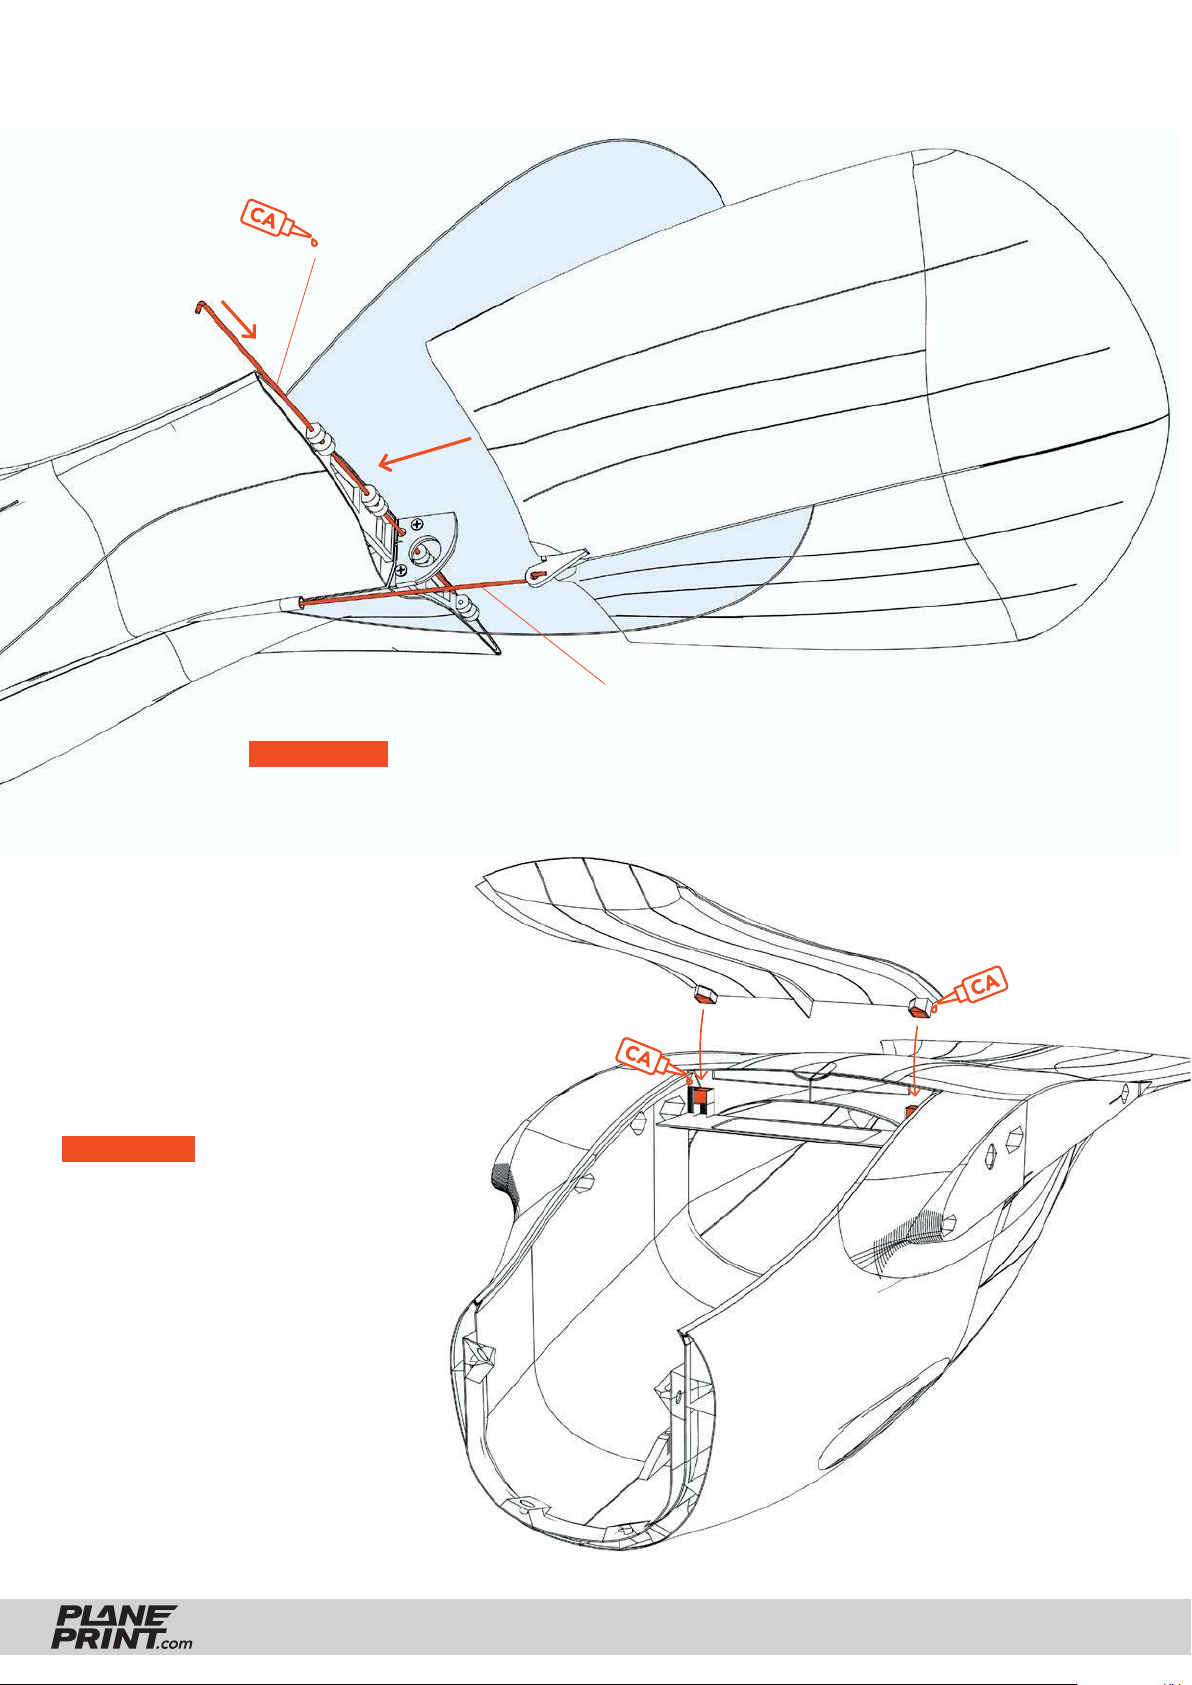
Fix the steel wire to the fuselage with a drop of CA glue.
medium l.
Steel wire Ø1*150mm
IMPORTANT The elevator must be easily movable!
Magnetic
cover fastener
Stick the four 5*5*5mm neodymium
magnets into the holes provided.
IMPORTANT Make sure that the
magnets are in the correct orientation
to each other and do not repel each
other!
Steel wire Ø1mm
The cover is inserted into the opening at the head and fixed with the
magnets at the back.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
25
Page 26
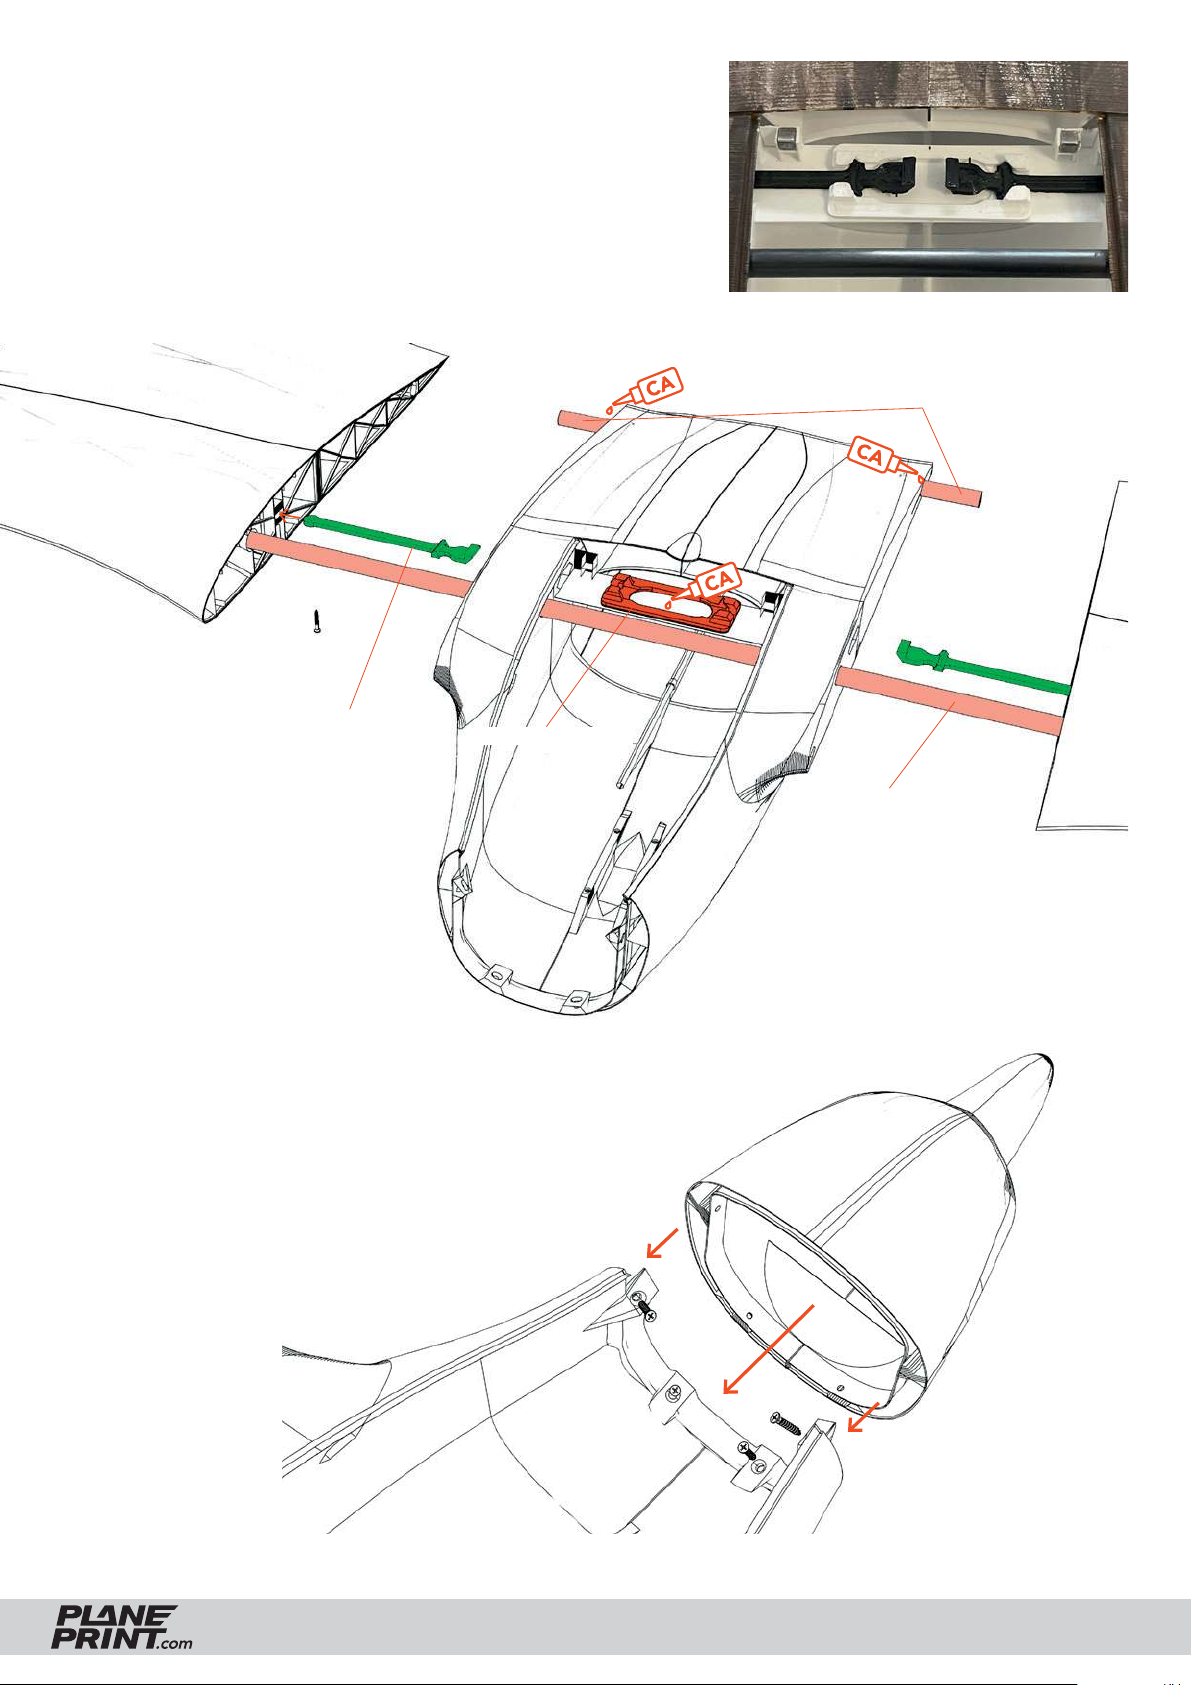
Wing fastening
Screw the TPU tensioners into
the wings, attach the wings
to the fuselage and clip the
tensioners into the frame.
Carbon rod Ø8*40mm
eagle-Parts-flex-profile4.stl
Head attachement
The head is screwed on from the inside
with four tapping screws 2*8mm and can
be exchanged for the motor head.
eagle-Parts-profile1.stl
Carbon rod Ø8*920mm
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
26
Page 27
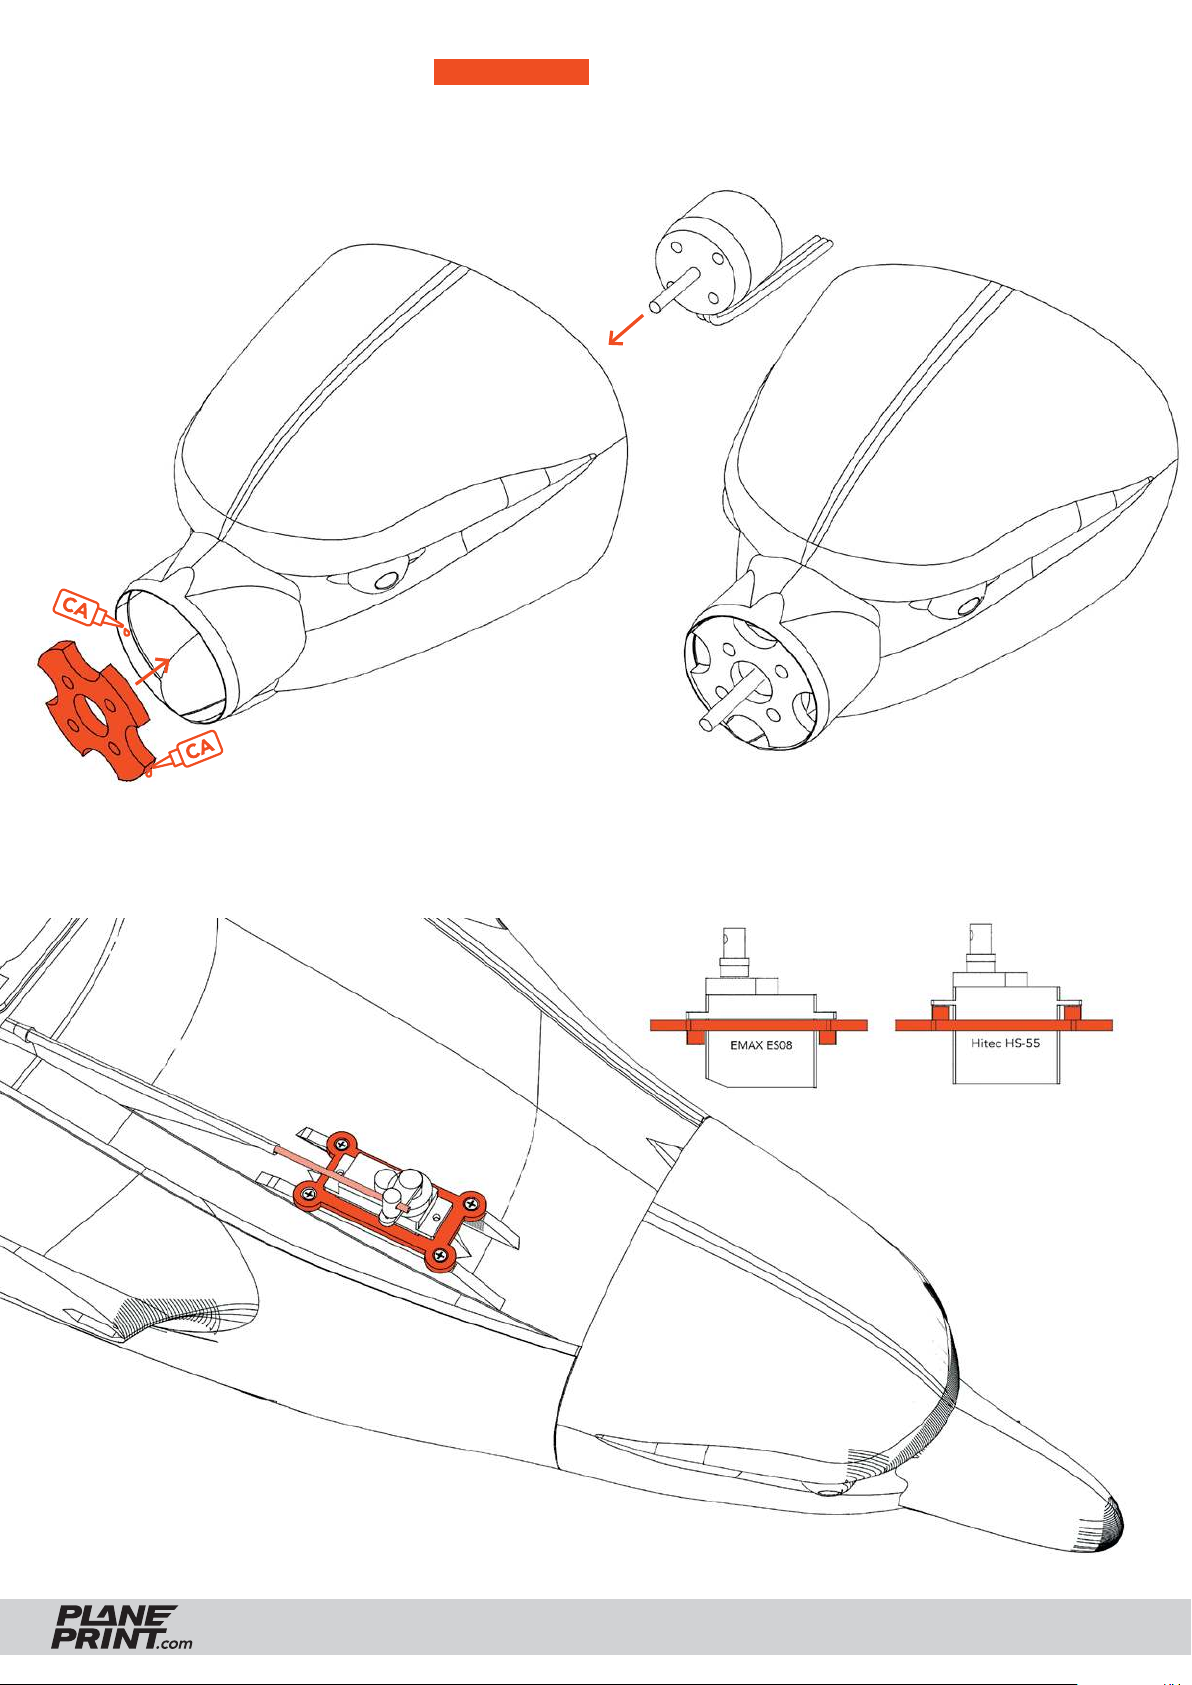
Motor mounting
eagle-Motorhead-profile3.stl
SAFETY FIRST Use appropriate screws for motor mounting to ensure
safe operation! Make sure the prop runs smoothly and does not generate
vibrations. Check regularly that the motor mounting is absolutely tight!
eagle-Motormount-profile1.stl
Servo Elevator
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
27
Page 28
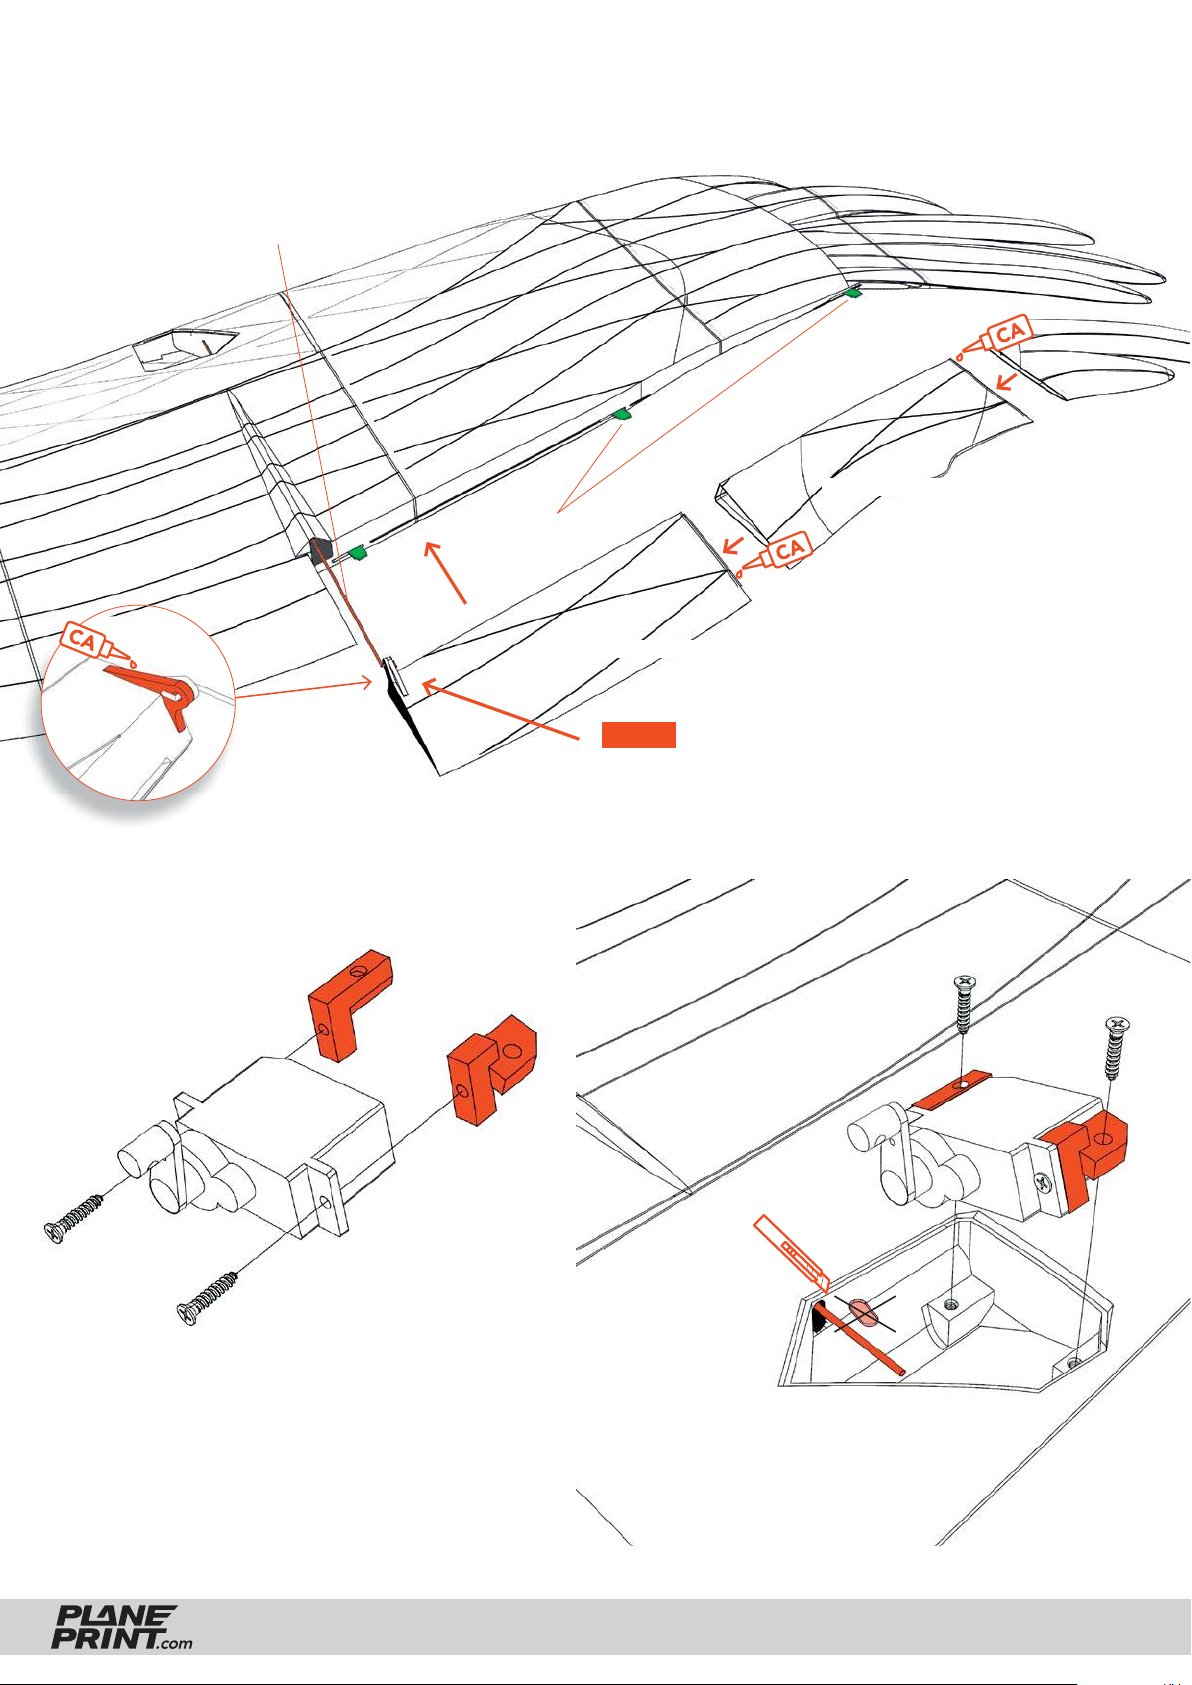
Aileron/Servo mounting – Example left side
Steel wire Ø1mm
eagle-Aileron2_LW-left-profi le3.stl
eagle-Parts-fl ex-profi le4.stl
eagle-Aileron3_LW-left-profi le3.stl
eagle-Aileron1_
LW-left-profi le3.stl
eagle-Parts-profi le1.stl
eagle-Wingservo_XXX-profi le1.stl
NOTE Put wire in before glueing.
When the servo is installed, fi x the cover
(eagle-Servocovers-profi le3.stl) with a tape.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
28
Page 29
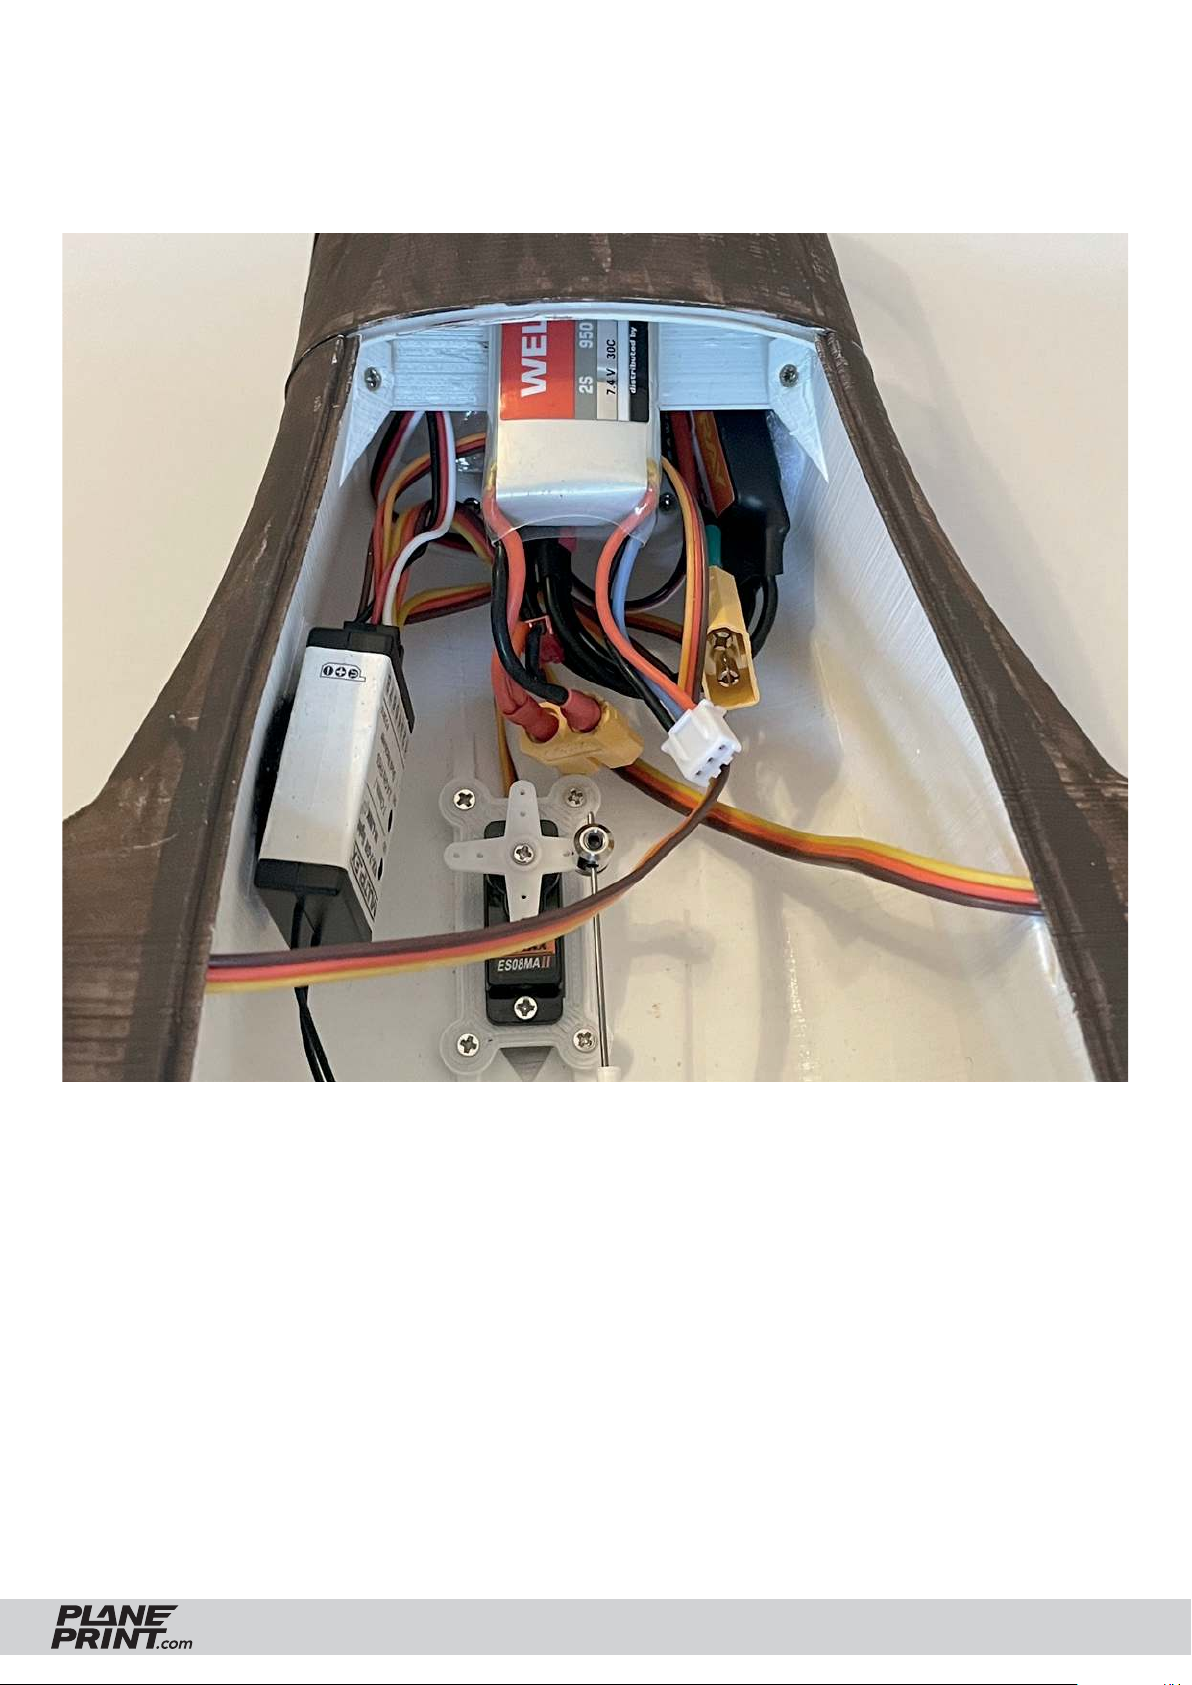
RC components
Attach the Controller, receiver and battery with self-adhesive Velcro.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
29
Page 30
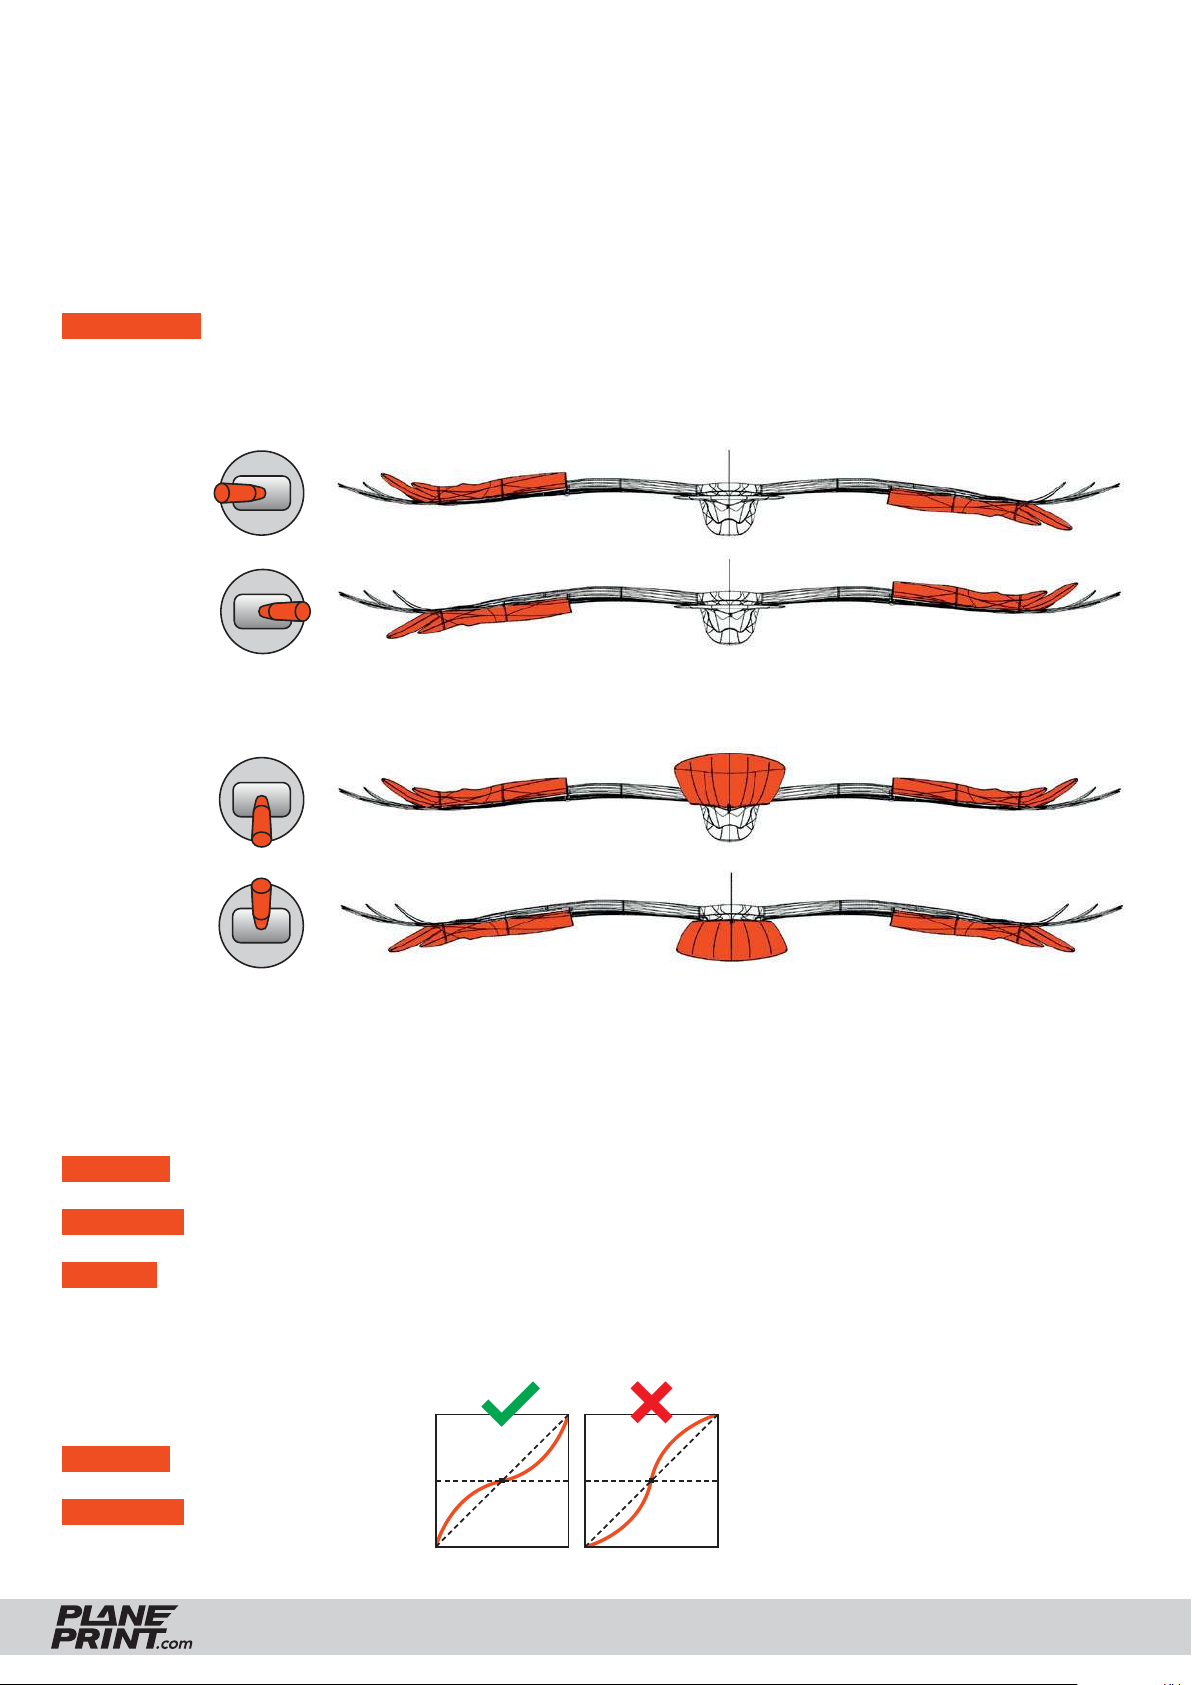
SETTINGS FOR FLYING
After installing the electronics and setting up the transmitter, check that the control surfaces are aligned correctly. Set the transmitter trim to zero. The ailerons should be aligned with the trailing edge of the wing tip.
Then align the flaps with the ailerons. The elevator should be aligned with the horizontal stabilizer and the
rudder to the vertical stabilizer. Change the position of the moving parts by changing the length of the linkage
from the servo arm to the control horn. In-flight adjustments can be made later with the trim.
IMPORTANT The eagle is programmed like a flying wing! This means that the ailerons also take over the
function of the elevator. In addition, the tail must be mixed with the elevator function.
Aileron
Elevator
Setting the servo travel
AILERON In the basic setting, the ailerons must point 2 mm upwards! up: 20 mm, down: 15 mm
ELEVATOR Ailerons: up 15 mm, down: 15 mm – Tail (see picture on the next page)
MOTOR At full throttle the elevator has to be corrected a little bit down with a mixer.
Try it carefully and be prepared for the eagle to pull up at full throttle!
Expo setting
(for some remote controls a minus
AILERON 20 %
has to be in front of the number)
ELEVATOR 20 %
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
30
Page 31
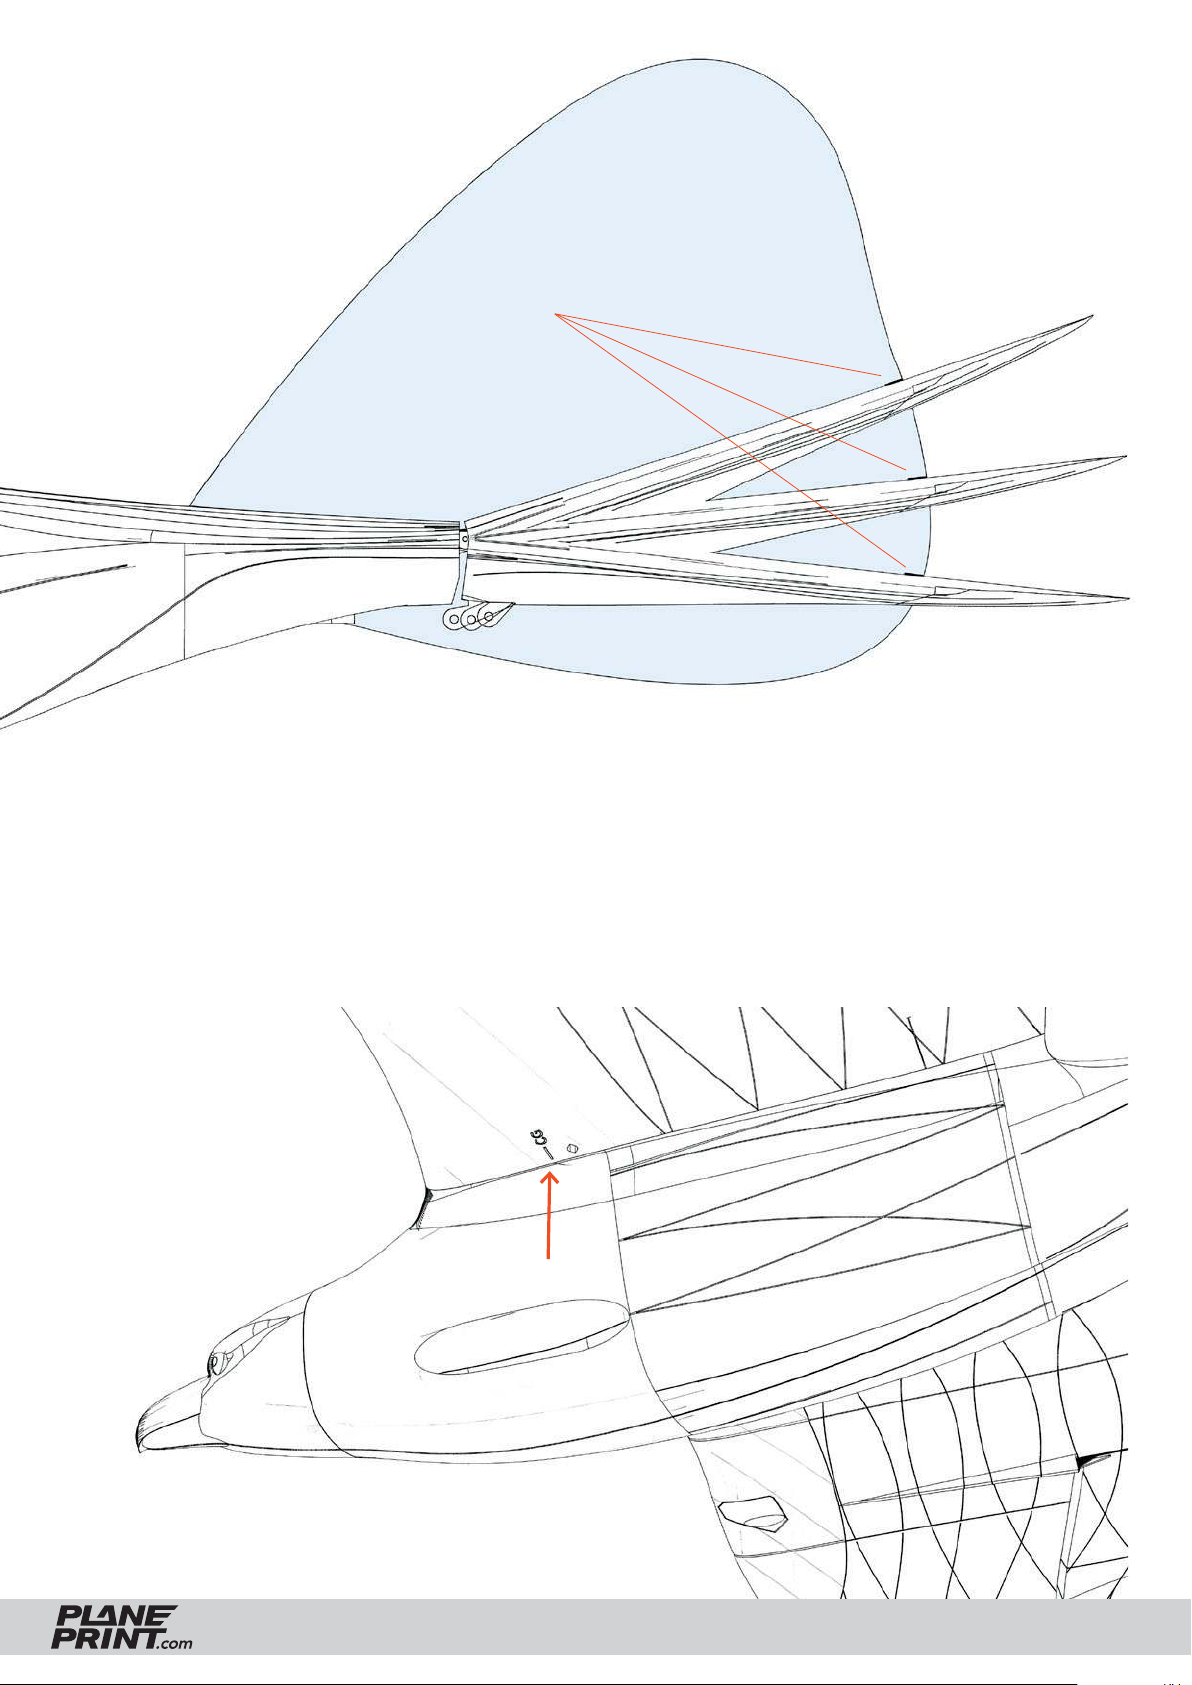
Markings on the rudder
Center of Gravity (CG)
up
Normal flight
down
The aircraft must balance precisely 66 mm/2.59 inches behind the leading edge (see markings on the fuse-
lage). For the first flight we recommend to move the center of gravity about 5 mm/0.2 inches further forward.
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
31
Page 32
Flight timer
Flight time will vary depending on the battery size. Expect 5 minutes under normal circumstances; however, it
may be possible to fly for much longer. It is a good idea to be conservative with the flight timer until you gain
experience with your airplane.
TECHNICAL SPECIFICATIONS
WINGSPAN 2000 mm/78.7 inches
LENGHT 806 mm/31.7 inches
FLIGHT WEIGHT 1160 grams (Motor version)
Please be aware of wildlife and fly the eagle
only in areas where it is allowed!
EAGLE
PRINTING & ASSEMBLING MANUAL
© PLANEPRINT
32
Page 33
AGE RECOMMENDATION 14+
NOT FOR CHILDREN UNDER 14 YEARS.
THIS IS NOT A TOY!
By using the download data, an RC model airplane, called
„model“ for short, can be manufactured using a 3D printer.
As a user of this model, only you are responsible for safe
operation that does not endanger you or others, or that
does not damage the model or property of others.
PLANEPRINT.com assumes no responsibility for damage to
persons and property caused by pressure, transport or use
of the product. Filaments, printing supplies, hardware or
consumables that can not be used after faulty 3D printing
will not be replaced by PLANEPRINT.com in any way.
When operating, always keep a safe distance from your
model in all directions to avoid collisions and injuries.
This model is controlled by a radio signal. Radio signals can
be disturbed from outside without being able to influence
it. Interference can lead to a temporary loss of control.
Always operate your model on open terrains, far from cars,
traffic and people.
Always follow the instructions and warnings for this product
and any optional accessories (servos, receivers, motors,
propellers, chargers, rechargeable batteries, etc.) carefully.
Avoid water contact with all components that are not specially designed and protected. Moisture damages the electronics.
Never take an item of the model or accessory in your mouth
as this can lead to severe injuries or even death.
Never operate your model with low batteries in the transmitter or model.
Always keep the model in view and under control.
Use only fully charged batteries.
Always keep the transmitter switched on when the model
is switched on.
Always remove the battery before disassembling the model.
Keep moving parts clean and dry at all times.
Always allow the parts to cool before touching them.
Always remove the battery after use.
Make sure that the Failsafe is properly set before the flight.
Keep all chemicals, small parts and electrical components
out of the reach of children.
We develop our models to the best of our knowledge and belief.
We accept no liability for consequential damage and injuries
caused by improper use. Please be careful when handling
motors, batteries and propellers and only move your model with
insurance and in approved places!
Never operate the model with damaged wiring.
Never touch moving parts.
© PLANEPRINT.com, A-6021 Innsbruck, Conradstraße 6, [email protected]
© Design STL files by René Marschall • Layout: marschall designlab, marschall.cc
 Loading...