

Page 1
Operator’s
Manual
SmartFab™ 125
Manual: 460801 Revision: Rev C 06/19
Original Language: English
Page 2
Cancer and Reproductive Harm -
8163361
www.P65warnings.ca.gov
This product and other products
could be protected by patents or
have patents pending. All the latest
patent information is available at
patent.mcelroy.com
Page 3
Introduction
Thank you for purchasing this
McElroy product
McElroy has created a smarter way to socket fuse pipe and
fittings for polypropylene piping systems with the SmartFab™
125 benchtop machine. Its portable design allows it to be
positioned on any flat surface for precise prefabrication,
providing versatility in the field as well as the shop.
Advanced features of the SmartFab 125 provide more efficiency
with innovative inserts that reduce ovality in pipe and fittings.
The heater pivots to easily accommodate fittings situated on
either side of the machine, which eliminates having to reposition
the entire machine. Its four jaws adjust to any desired spacing
and each jaw clamps individually to the desired pipe and fitting
size.
The SmartFab 125 socket fuses 20mm to 125mm pipe and
fittings.
When fusing thermoplastic pipe materials, refer to the pipe
manufacturer's fusion procedures or appropriate joining
standard.
With reasonable care and maintenance, this machine will give
years of satisfactory service.
TX04887-03-15-16
Before operating this machine, please read this manual
thoroughly, and keep a copy with the machine for future
reference. This manual is to be considered part of your machine.
CD01407-11-12-15
McElroy University
For more than 30 years, McElroy has been the only pipe
fusion machine manufacturer to continuously offer advanced
training. Course offerings are meant to enhance your efficiency,
productivity and safety in the proper use of McElroy machines.
McElroy University classes are structured so that the skills
learned and the machines used in each class closely match
the machines found on pipelining jobsites. We offer training at
our facility or yours. Our uniquely qualified McElroy University
course instructors offer years of industry experience.
Tuition for each course includes lunches, course materials and
a certificate of completion. Online registration, as well as
up-to-date course offerings and dates, is available at www.
mcelroy.com/university
This manual is intended as a guide only and does not take the
place of proper training by qualified instructors. The information
in this manual is not all inclusive and can not encompass all
possible situations that can be encountered during various
operations.
MU2-03-13-14
TX04659-03-24-14
Page 4
Warranty
LIMITED WARRANTY
McElroy Manufacturing, Inc. (McElroy) warrants all products
manufactured, sold and repaired by it to be free from defects in
materials and workmanship, its obligation under this warranty
being limited to repairing or replacing at its factory and new
products, within 5 years after shipment, with the exception of
purchased items (such as electronic devices, pumps, switches,
etc.), in which case that manufacturer’s warranty applies.
Warranty applies when returned freight is prepaid and which,
upon examination, shall disclose to have been defective. This
warranty does not apply to any product or component which
has been repaired or altered by anyone other than McElroy or
has become damaged due to misuse, negligence or casualty,
or has not been operated or maintained according to McElroy’s
printed instructions and warnings. This warranty is expressly in
lieu of all other warranties expressed or implied. The remedies
of the Buyer are the exclusive and sole remedies available
and Buyer shall not be entitled to receive any incidental or
consequential damages. Buyer waives the benefit of any rule
that disclaimer of warranty shall be construed against McElroy
and agrees that such disclaimers herein shall be construed
liberally in favor of McElroy.
RETURN OF GOODS
Buyer agrees not to return goods for any reason except upon
the written consent of McElroy obtained in advance of such
return, which consent, if given, shall specify the terms and
conditions and charges upon which any such return may be
made. Materials returned to McElroy, for warranty work, repair,
etc., must have a Return Material Authorization (RMA)
number, and be so noted on the package at time of shipment.
For assistance, inquiry shall be directed to:
McElroy Manufacturing, Inc.
P.O. Box 580550
833 North Fulton Street Tulsa, Oklahoma 74158-0550
PHONE: (918) 836–8611, FAX: (918) 831–9285.
EMAIL: [email protected]
Note: Certain repairs, warranty work, and inquiries may be
directed, at McElroy’s discretion, to an authorized service center
or distributor.
DISCLAIMER OF LIABILITY
McElroy accepts no responsibility of liability for fusion joints.
Operation and maintenance of the product is the responsibility
of others. We recommend qualified joining procedures be
followed when using McElroy fusion equipment.
McElroy makes no other warranty of any kind whatever, express
or implied; and all implied warranties of merchantability and
fitness for a particular purpose which exceed the aforestated
obligation are hereby disclaimed by McElroy.
PRODUCT IMPROVEMENT
McElroy reserves the right to make any changes in or
improvements on its products without incurring any liability or
obligation to update or change previously sold machines and/
or the accessories thereto.
INFORMATION DISCLOSED
No information of knowledge heretofore or hereafter disclosed
to McElroy in the performance of or in connection with the terms
hereof, shall be deemed to be confidential or proprietary, unless
otherwise expressly agreed to in writing by McElroy and any
such information or knowledge shall be free from restrictions,
other than a claim for patent infringement, is part of the
consideration hereof.
PROPRIETARY RIGHTS
All proprietary rights pertaining to the equipment or the
components of the equipment to be delivered by McElroy
hereunder, and all patent rights therein, arising prior to, or in the
course of, or as a result of the design or fabrication of the said
product, are exclusively the property of McElroy.
LAW APPLICABLE
All sales shall be governed by the Uniform Commercial Code of
Oklahoma, U.S.A.
Register your product online to activate your warranty:
www.McElroy.com/fusion
(Copy information listed on the machine nameplate here for your
records).
TX02486-11-4-13
Model No.
Serial No.
Date Received
Distributor
Page 5
Equipment Safety
Safety Alerts .........................................................1-1
Read and Understand .................................................1-1
General Safety .......................................................1-2
Wear Safety Equipment ................................................1-2
Heater is Not Explosion Proof ...........................................1-2
Electrical Safety ......................................................1-3
Pinch Points ..........................................................1-3
Heater is Hot .........................................................1-3
Fusion Procedures .....................................................1-3
Overview
Theory of Heat Fusion .................................................. 2-1
SmartFab™ 125 Fusion Machine .........................................2-2
Carriage Assembly ....................................................2-2
Heater ..............................................................2-3
Carriage Jaws and Inserts ..............................................2-4
Depth Star ...........................................................2-4
Jaw Clamp Handles ...................................................2-5
Jaw Frame Lock Handles ...............................................2-5
Set Up Gauge ........................................................2-5
Table of Contents
Set Up
Set Up Calibration ....................................................3-1
Fusion Procedure
Read Before Operating ................................................4-1
Level Machine ........................................................4-1
Connecting to Power ..................................................4-1
Prepare Heater .......................................................4-1
Install Inserts .........................................................4-2
Load Pipe and Fitting ..................................................4-2
Support Pipe .........................................................4-3
Verify Alignment ......................................................4-3
Check Heater Temperature. . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . . 4-3
Heating the Pipe and Fitting .............................................4-4
Remove Heater .......................................................4-4
Inspect Melt ..........................................................4-4
Fusion and Cooling ....................................................4-5
Opening Jaws ........................................................4-5
COPYRIGHT © 2019, 2016, 2015
McELROY MANUFACTURING, INC.
Tulsa, Oklahoma, USA
All rights reserved
All product names or trademarks are property of their respective owners. All information, illustrations
and specifications in this manual are based on the latest information available at the time of
publication. The right is reserved to make changes at any time without notice.
Page 6
Maintenance
Preventative Maintenance ..............................................5-1
Cleaning the Machine .................................................5-1
Clean Jaws and Inserts .................................................5-1
Fasteners Must Be Tight ................................................5-2
Installing Socket Fusion Adapters ........................................5-2
Clean Heater Surfaces .................................................5-2
Adjusting Heater Temperature ...........................................5-2
Heater Indicator Light ..................................................5-3
Maintenance Checklist
Fusion Machine Checklist ...............................................6-1
Specifications
Fusion Machine Specifications: SmartFab™ 125 ............................7-1
Table of Contents
Page 7
Fusion Equipment Safety
Safety Alerts
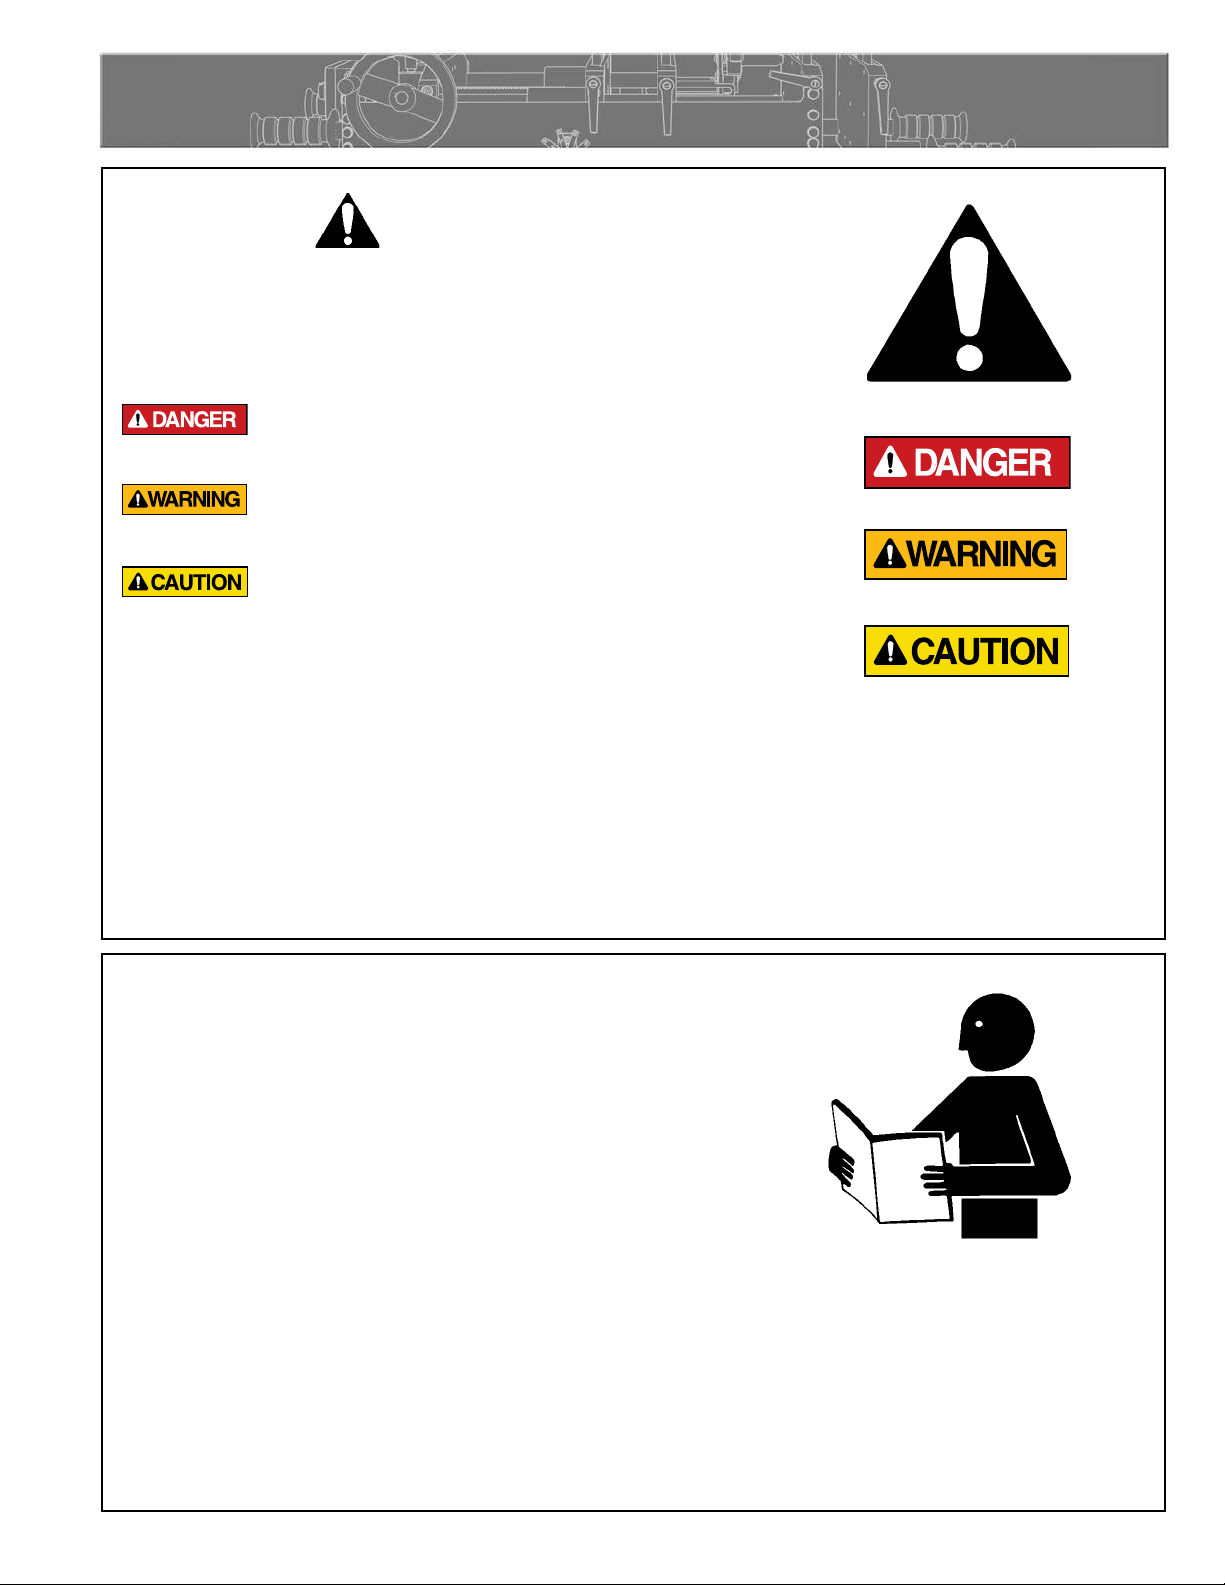
This hazard alert sign appears in this manual. When
you see this sign, carefully read what it says. YOUR SAFETY IS
AT STAKE.
You will see the hazard alert sign with these words: DANGER,
WARNING, and CAUTION.
Indicates an imminently hazardous situation
which, if not avoided, will result in death or
serious injury.
Indicates a potentially hazardous situation
which, if not avoided, could result in
death or serious injury.
Indicates a hazardous situation which,
if not avoided, may result in minor or
moderate injury.
In this manual you should look for two other words: NOTICE
and IMPORTANT.
NOTICE: can keep you from doing something that might
damage the machine or someone's property. It may also be
used to alert against unsafe practices.
IMPORTANT: can help you do a better job or make your job
easier in some way.
WR00051-11-30-92
TX00030-12-1-92
Read and Understand
Do not operate this equipment until you have carefully read, and understand
all the sections of this manual, and all other equipment manuals that will be
used with it.
Your safety and the safety of others depends upon care and judgment in
the operation of this equipment.
Follow all applicable federal, state, local, and industry specific regulations.
McElroy Manufacturing, Inc. cannot anticipate every possible
circumstance that might involve a potential hazard. The warnings in this
manual and on the machine are therefore not all inclusive. You must satisfy
yourself that a procedure, tool, work method, or operating technique is
safe for you and others. You should also ensure that the machine will not be
damaged or made unsafe by the method of operation or maintenance you
choose.
TX02946-4-15-09
WR00052-12-1-92
1 - 1
Page 8
Fusion Equipment Safety
General Safety
Safety is important. Report anything unusual that you notice during set up
or operation.
LISTEN for thumps, bumps, rattles, squeals, air leaks, or unusual sounds.
SMELL odors like burning insulation, hot metal, burning rubber, hot oil, or
natural gas.
FEEL any changes in the way the equipment operates.
SEE problems with wiring and cables, hydraulic connections, or other
equipment.
REPORT anything you see, feel, smell, or hear that is different from what
you expect, or that you think may be unsafe.
TX00114-4-22-93
Wear Safety Equipment
Wear a hard hat, safety shoes, safety glasses, and other applicable
personal protective equipment.
Remove jewelry and rings, and do not wear loose-fitting clothing or long
hair that could catch on controls or moving machinery.
SAFE1ST-12-22-92
WR00053-12-2-92
TX00032-4-7-93
Heater Is Not Explosion Proof
This heater is not explosion proof. Operation of heater in an
explosive atmosphere will result in serious injury or death.
Heater components are attached to the machine and the machine must not be used
in an explosive atmosphere.
WR00034-11-30-92
TX04846-12-14-15
1 - 2
Page 9
Fusion Equipment Safety
Electrical Safety
Always ensure equipment is properly
grounded. It is important to remember that
you are working in a wet environment with
electrical devices. Proper ground connections
help to minimize the chances of an electric
shock.
Frequently inspect electrical cords and unit for damage. Have
damaged components replaced and service performed by a
qualified electrician.
Do not carry electrical devices by the cord
NOTICE: Always connect units to the proper power source as listed on the
unit, or in the owner's manual.
TX00105-6-12-13
Pinch Points
Moving components of the machine can create pinch
points. Use caution while operating the machine not to
expose body parts to pinch points. Pinch points may
cause minor to moderate injury.
WR00055-4-7-93
WR00025-11-30-92
TX04847-12-14-15
Heater is Hot
The heater is hot and will burn clothing and skin. Use
care when heating the pipe and fitting.
NOTICE: Use only a clean dry lint free non-synthetic cloth to clean the
heater adapters.
TX04848-12-14-15
Fusion Procedures
Obtain a copy of the pipe manufacturer's procedures or appropriate
joining standard for the pipe being fused. Follow the procedure carefully,
and adhere to all specified parameters.
NOTICE: Failure to follow pipe manufacturer's procedure could
result in a bad joint. Always follow pipe manufacturer's
procedures.
TX04469-10-24-12
WR00030-2-10-93 WR00114-11-30-15
WR00079-1-24-96
1 - 3
Page 10
Overview
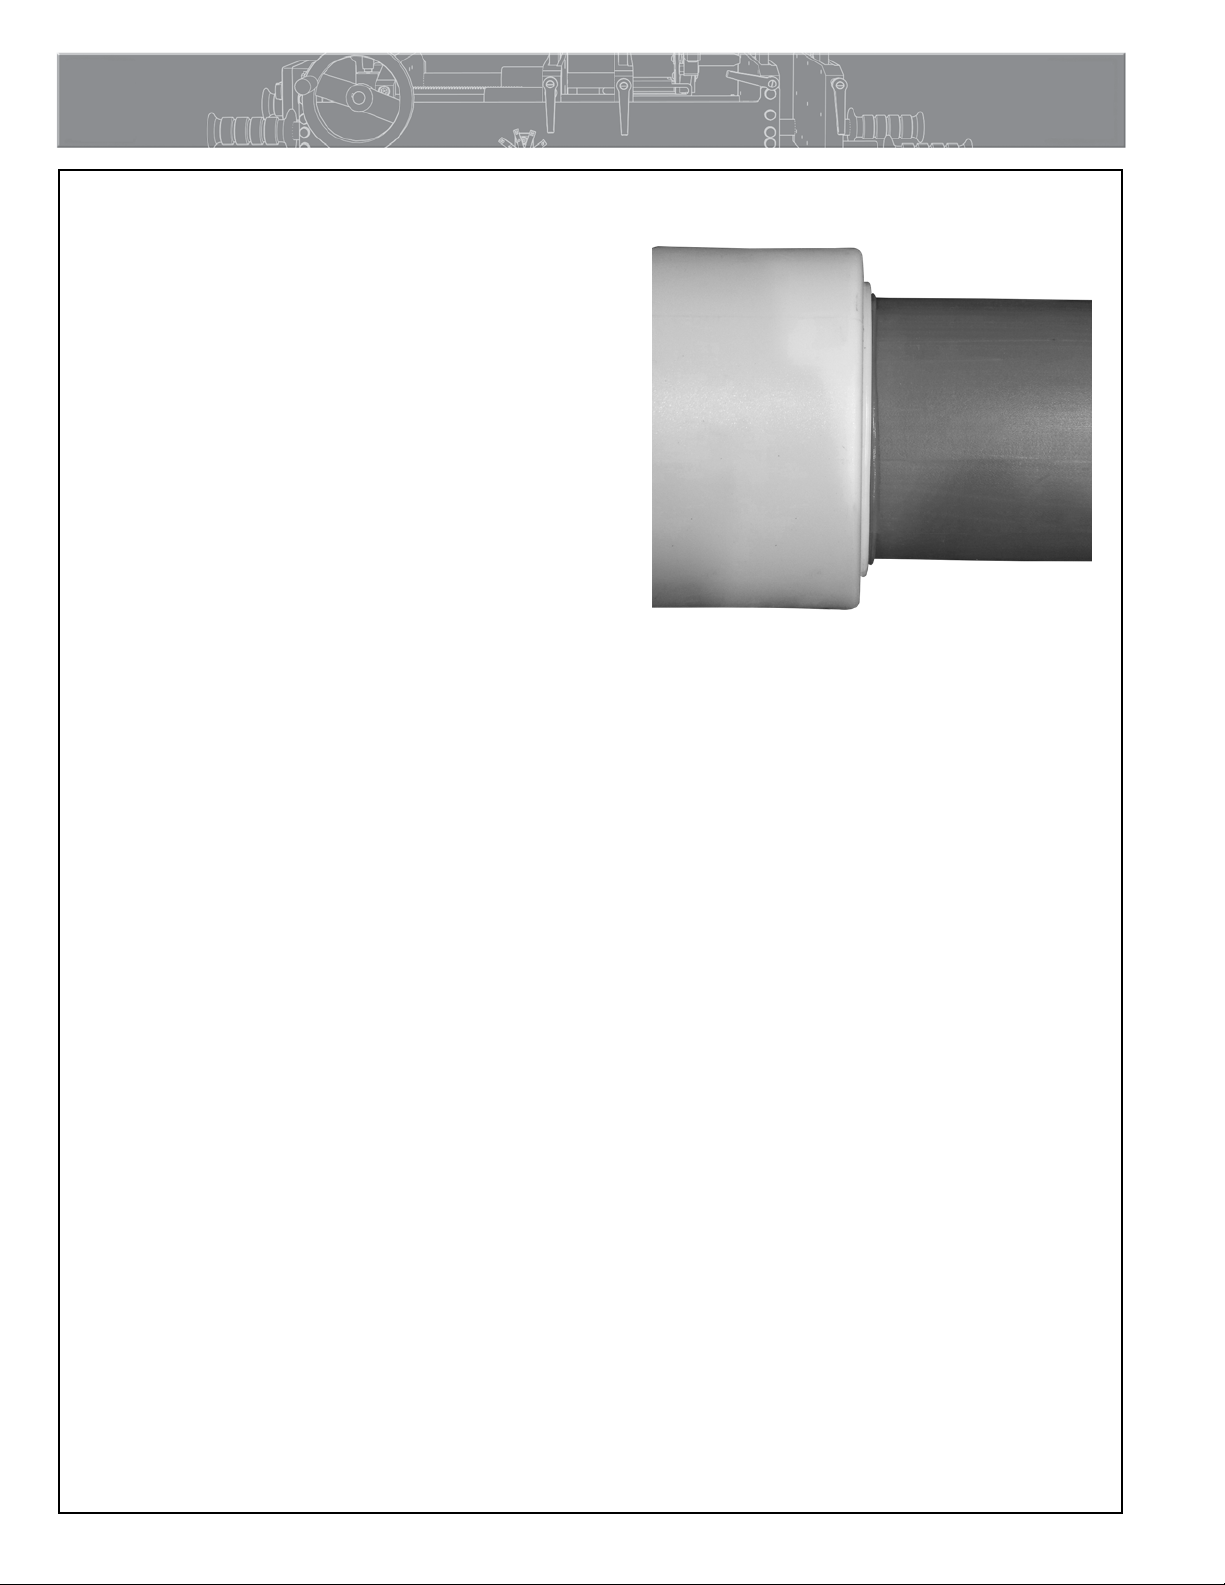
Theory of Heat Fusion
The principle of heat fusion is to heat two surfaces to a designated
temperature, and then fuse them together by application of force. This
develops pressure which causes flow of the melted materials, which
causes mixing and thus fusion. When the thermoplastic material is
heated, the molecular structure is transformed from semi-crystalline into
an amorphous condition. When fusion pressure is applied, the molecules
from each thermoplastic part mix. As the joint cools, the molecules return
to their semi-crystalline form, the original interfaces are gone, and the
fitting and pipe have become one monolithic unit. A strong, fully leak tight
connection is the result.
The principal operations include:
Clamping The pipe and fitting must be held firmly to allow all
subsequent operations to take place.
Cleaning The area of pipe that the fitting will come in contact with
must be cleaned.
Aligning The fitting, heater adapters, and pipe must be properly
aligned.
Heating A melt pattern must be formed that penetrates into the pipe
and into the fitting.
Joining The pipe and fitting must be joined and the pipe fully seated
within the fitting.
Holding The molten joint must be held immobile until adequately
cooled.
Inspecting Visually examine the entire circumference of the joint for
compliance with standards established by your company,
customer, industry, federal, state, or local regulations.
PH05429-11-24-15
TX04696-04-10-14-
2 - 1
Page 11
Overview
SmartFab™ 125 Fusion Machine
McElroy has created a smarter way to socket fuse pipe and fittings for
polypropylene piping systems with the SmartFab™ 125 benchtop machine.
Its portable design allows it to be positioned on any flat surface for precise
prefabrication, providing versatility in the field as well as the shop.
When fusing thermoplastic pipe materials, refer to the pipe manufacturer's
fusion procedures or appropriate joining standard.
The SmartFab 125 socket fuses 20mm to 125mm pipe and fittings.
TX04849-12-14-15
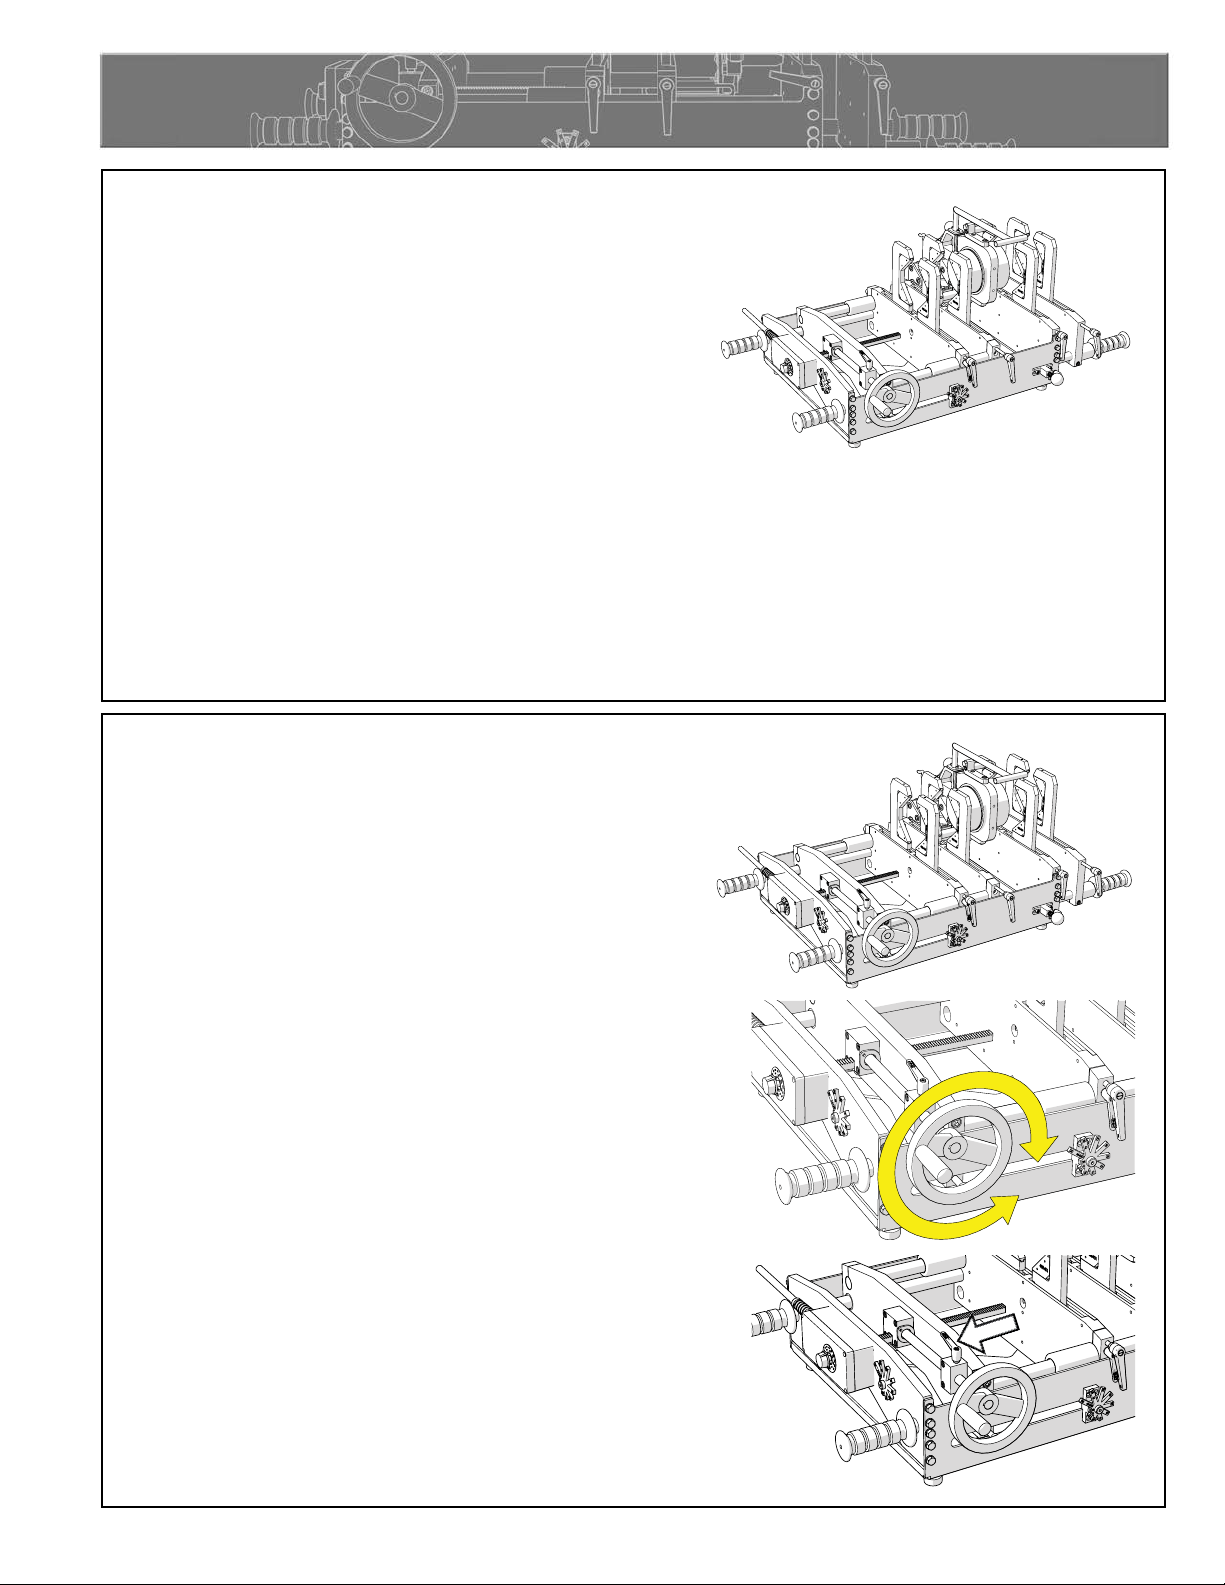
Carriage Assembly
The SmartFab 125 carriage assembly has 4 jaw frames which can be
individually spaced and clamped allowing the operator flexibility to fuse
the greatest combination of pipe and fittings.
The carriage consists of two fixed jaws and two movable jaws.
The movable jaws are actuated by a rack and pinion.
The movable jaws are opened and closed using the hand wheel on the
side of the machine.
The movable jaws can be locked in position by tightening the handle near
the hand wheel.
CD01407-11-12-15CD01407-11-30-15 CD01417-11-30-15 CD01407-11-12-15
TX04850-12-14-15
2 - 2
Page 12
Overview
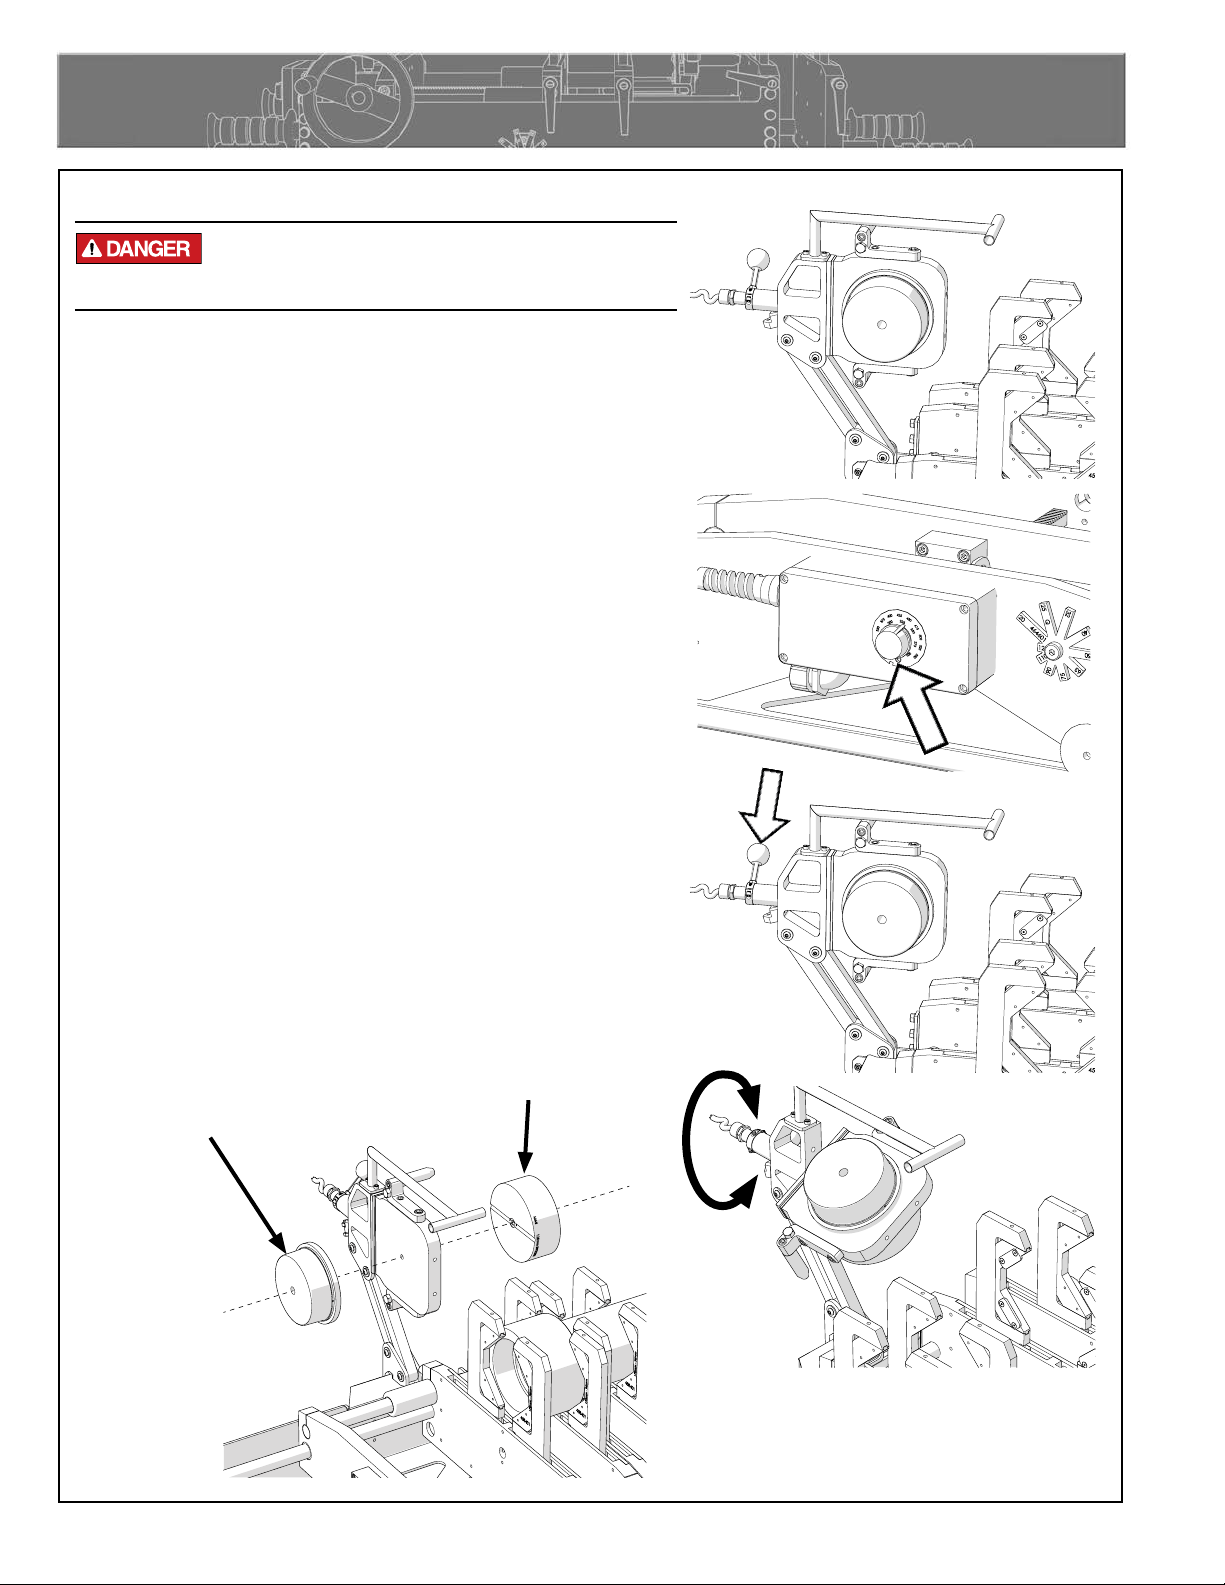
Heater
Heater is not explosion proof. Operation of heater in an
explosive atmosphere will result in serious injury or death.
The heater has a green indicator light which will flash on and off. This
indicates that the controller is operating normally. If the green indicator is
not flashing then the controller may not be operating properly. If this occurs,
disconnect power and have the heater repaired by a McElroy Authorized
Service Center.
The heater temperature is controlled by a microprocessor. It has a red indicator
light on the bottom of the temperature scale. When the heater is plugged in
and preheating the light glows steadily until the set temperature is reached. The
light then goes off and on slowly as the heater maintains temperature.
The heater body is not coated. Coated socket fusion heater adapters are
available for all socket fusion applications.
NOTICE: The heater should never be used without socket fusion heater
adapters installed.
To prevent a build-up of plastic pipe residue from accumulating on the heater
adapters (loss of surface temperature and pipe sticking may result), the heater
adapters should be cleaned with a clean dry lint free non-synthetic cloth before
every fusion joint.
The heater pivots in and out of the fusion area. The heater can be rotated to
change the position of the heater adapters from one side to the other to allow
fusion on both ends of the machine.
To rotate the heater, pull the handle of the heater with the round ball toward
the heater and rotate the heater.
CD01411-11-30-15CD01411-11-30-15
CD01440-11-23-15CD01415-11-23-15
Fitting Heater Adapter
TX04851-12-14-15
Pipe Heater Adapter
CD01452-12-01-15
2 - 3
Page 13
Overview
Carriage Jaws and Inserts
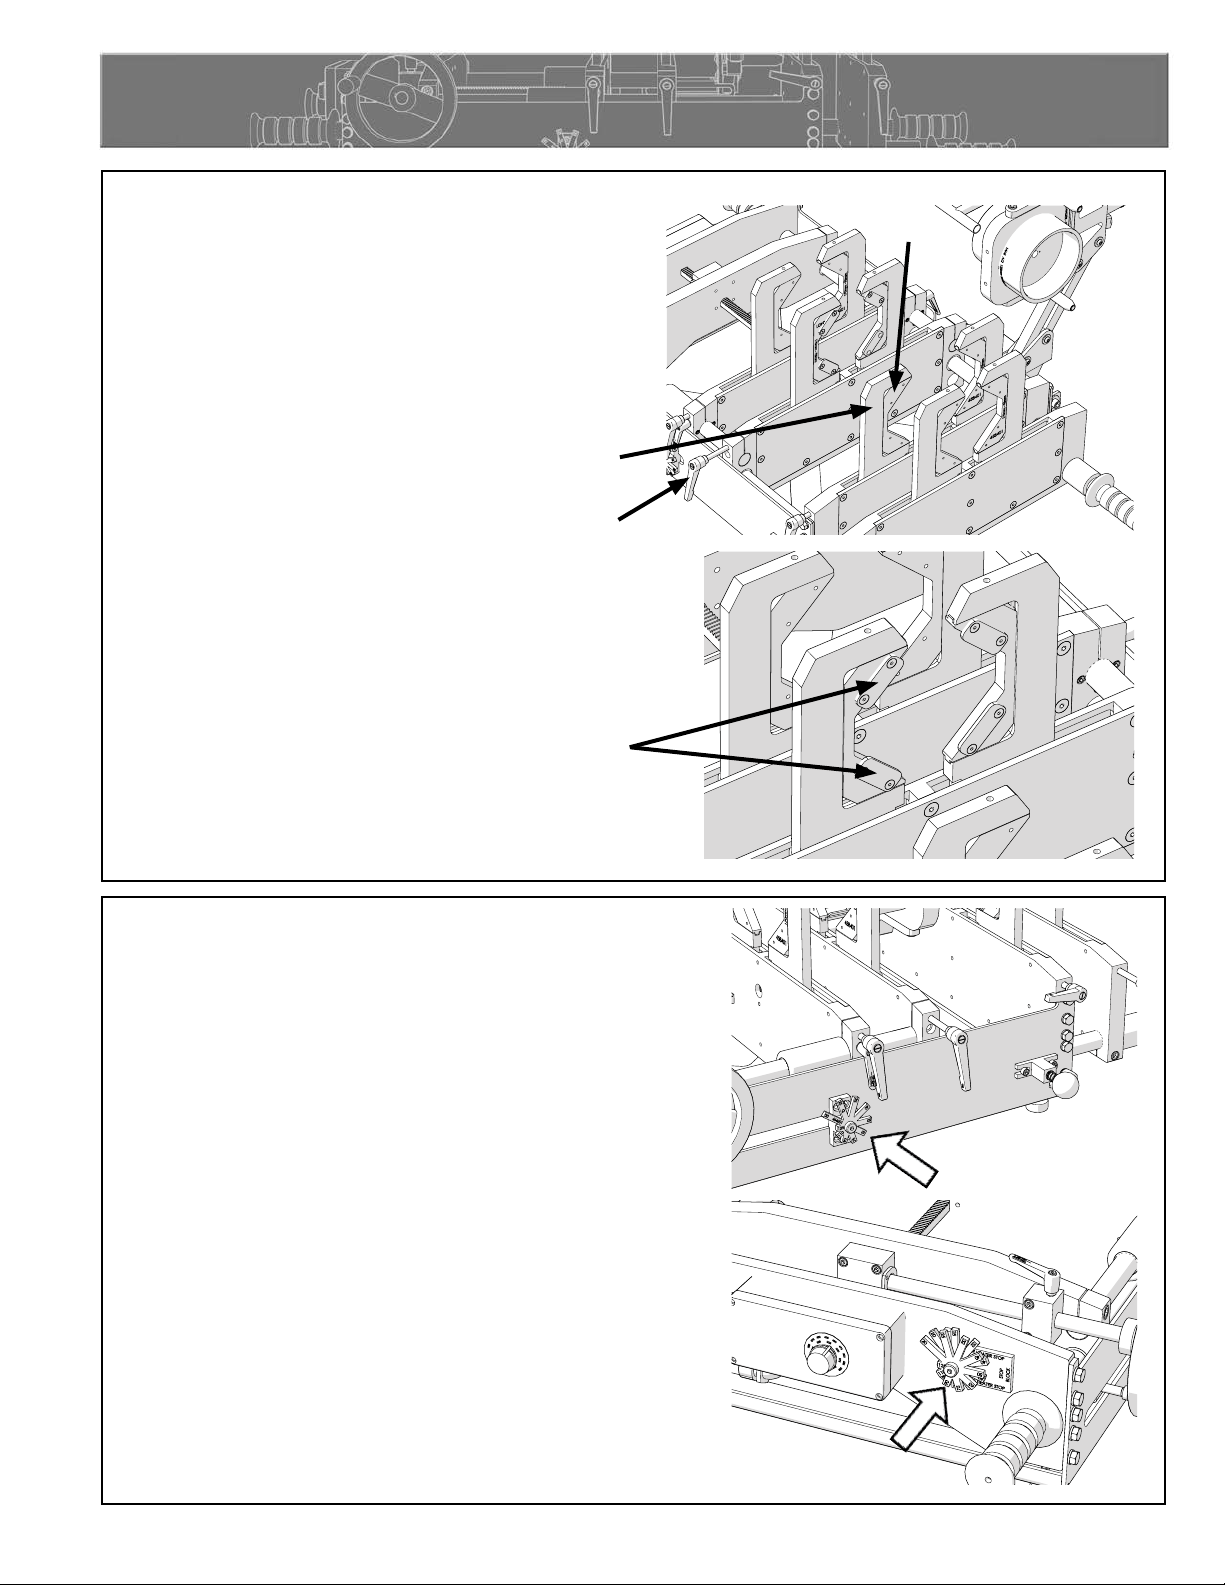
Each jaw frame has two insert holders and the jaws are opened
and closed using the handle at the end of the jaw frame.
Inserts are installed into the insert holders on each jaw frame.
Inserts are locked into place by a spring detent in the insert
holder. The inserts with the stop tabs are for the fitting and are
installed on the inner jaw frame on the same side as the socket
heater adapter on the heater.
Insert Holder
Jaw Open/
Close Handle
Insert
CD01412-12-10-15CD01457-12-09-15
Stop Tabs
TX04852-12-14-15
Depth Star
The depth star is used to change the stab depth of movable jaws by providing
a stop for the movable jaws to rest against. It rotates to change the pipe size to
fuse and each size is labeled on the face of the depth star.
There is a depth star to match the appropriate heater adapters. The depth stars
have a marking that will match the marking of the heater adapters.
The depth stars that are not being used are stored at the end of the machine
next to the heater controls when not in use.
CD01408-11-12-15
CD01456-12-10-15
TX04853-12-14-15
2 - 4
Page 14
Overview
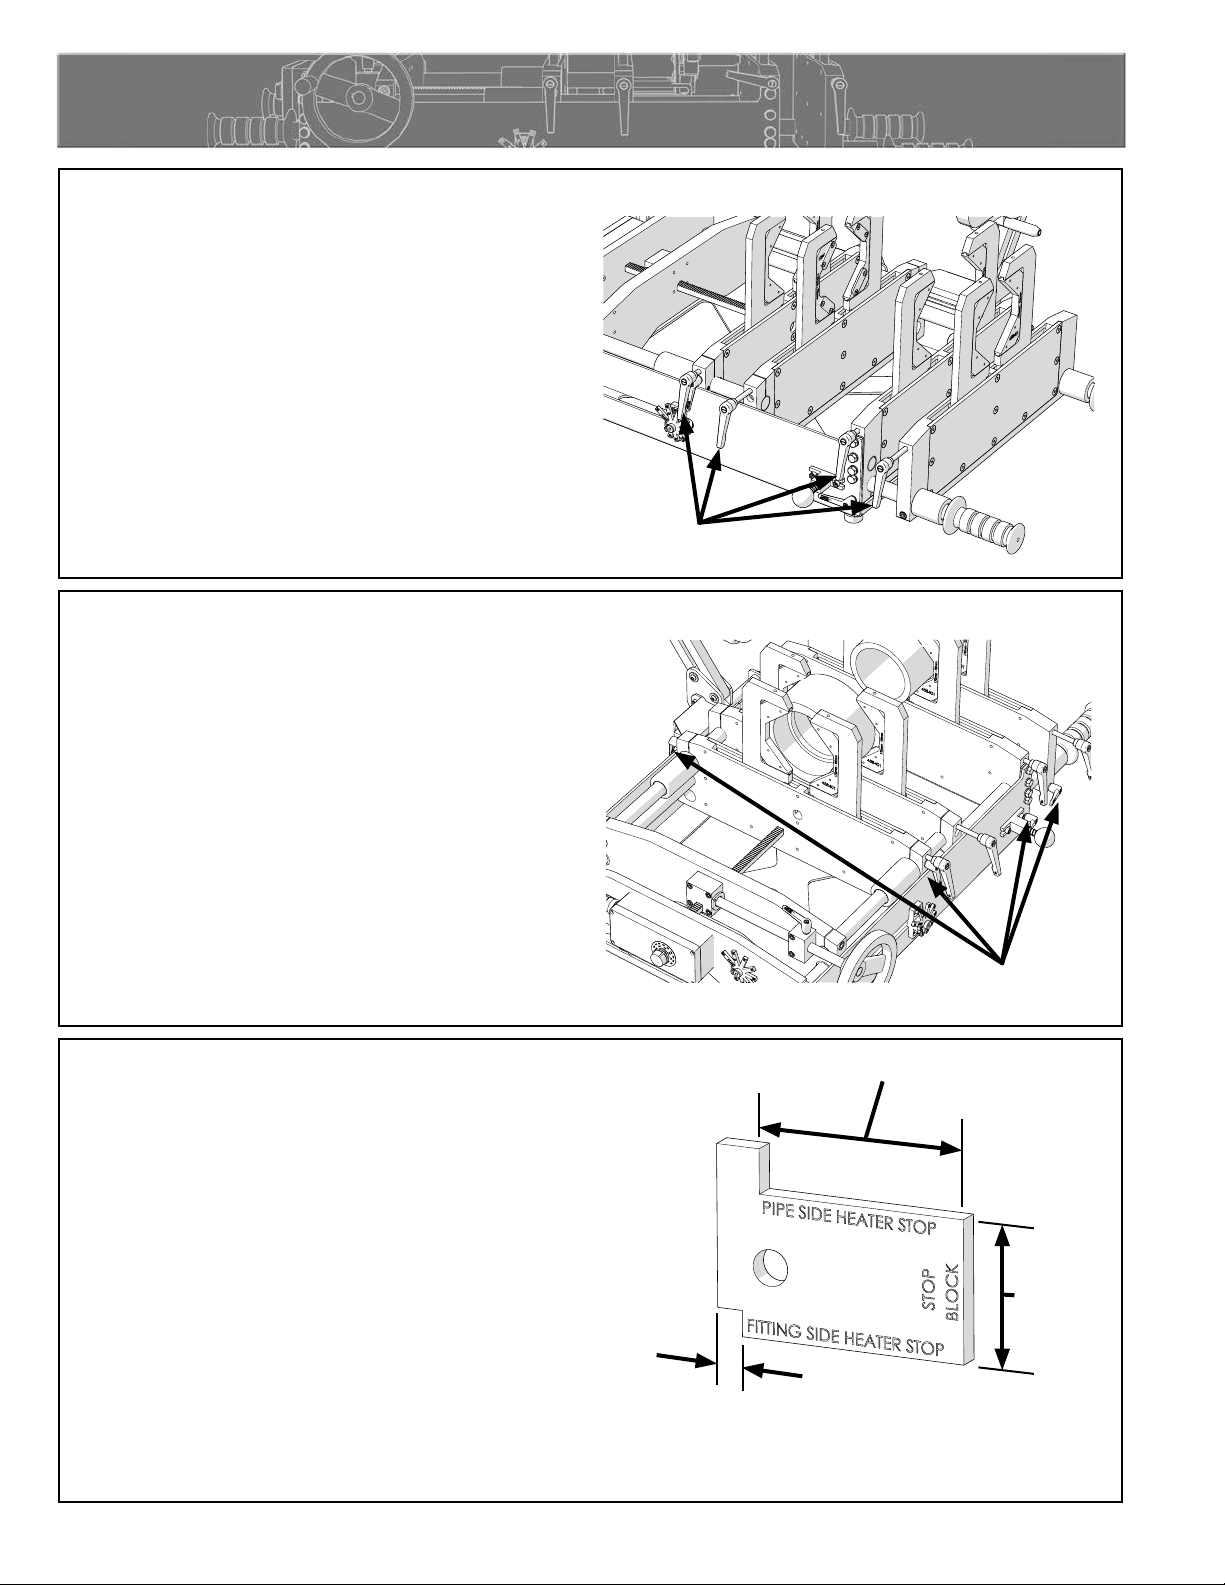
Jaw Clamp Handles
At the end of each jaw frame are adjustable handles for
clamping and unclamping of pipe and fittings. By pulling out on
the handles, the handle position can be adjusted.
Rotating the handle will open and close the jaws on the jaw
frame.
CD01413-11-20-15CD01444-11-30-15CD01444-11-30-15
TX04854-12-14-15
Jaw Clamp Handles
Jaw Frame Lock Handles
At both ends of three of the jaw frames are adjustable handles
for locking and unlocking the position of the jaw frames. By
pulling out on the handles, the handle position can be adjusted.
Rotating the handle will loosen and tighten the jaw frames on the
guide rods of the machine.
TX04855-12-14-15
Set Up Gauges
The machine comes with set up gauges for use during the set
up calibration procedures. There is a set up gauge to match the
appropriate heater adapters. The set up gauges will have a marking
that will match the marking of the heater adapters. There are 3 different
gauges on the block.
1) Pipe Side Heater Stop - to measure the long heater stop distance.
2) Fitting Side Heater Stop - to measure the short heater stop
distance.
3) Stop Block - to measure the distance between the two inner jaw
frames.
The gauges are stored with the additional depth stars when not in use.
Jaw Frame Lock
Handles
Pipe Side Heater Stop
Stop Block
Fitting Side
Heater Stop
TX04856-03-14-16
2 - 5
Page 15
Set Up
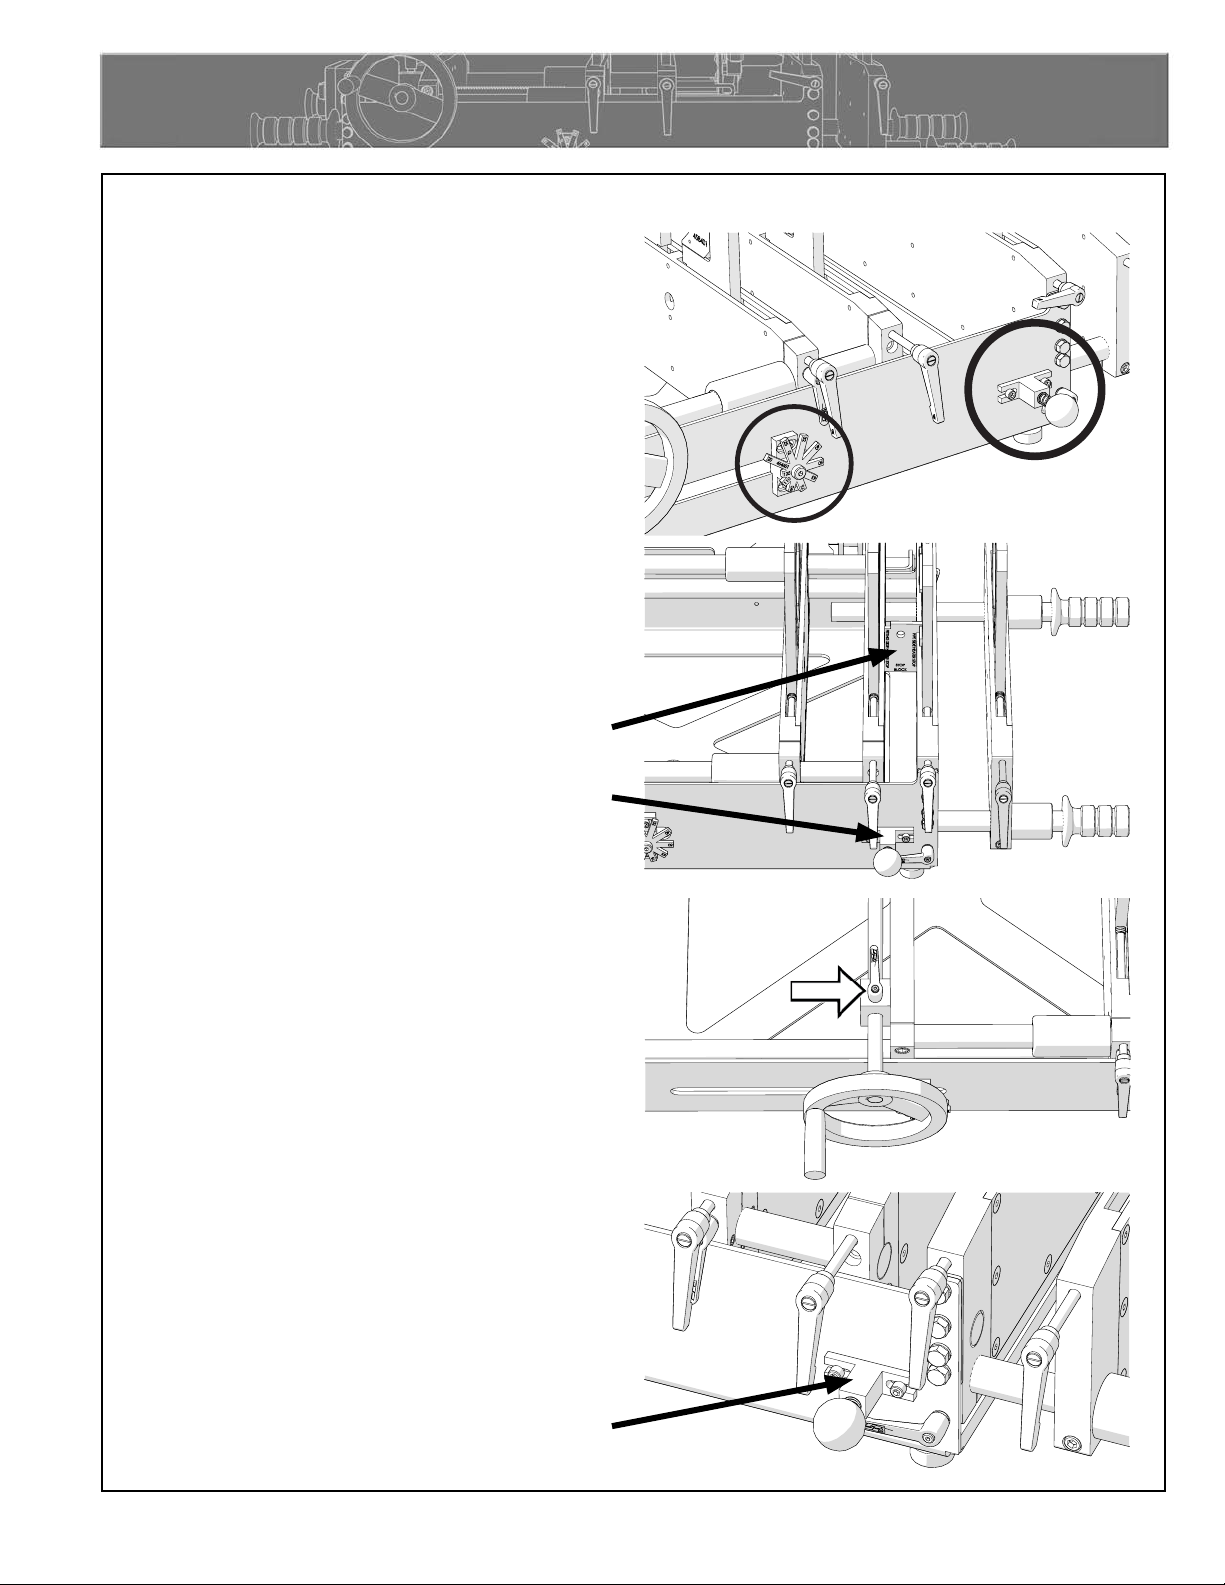
Set Up Calibration
Install the appropriate type depth star that will match the heater
adapters used.
Select the appropriate Set Up Gauge for the heater adapters
being used and use that gauge for the calibration procedures.
Loosen the bolts attaching the setting stop block and depth star
block to the frame.
Push in and hold the setting stop. Insert the appropriate Set Up
Gauge that matches the heater adapters used, between the inner
jaw frames with the stop block portion down. Close the carriage
until the inner jaw frames are resting against the Set Up Gauge.
CD01418-11-23-15CD01419-11-23-15CD01420-11-23-15
Set Up Gauge
Setting Stop Block
Lock the carriage. Adjust the setting stop block until it rests against
the inner jaw frame on the movable jaws.
Tighten the bolts on setting stop block.
Unlock the carriage. Open and close the carriage against the
setting stop and verify the measurement between the inner jaw
frames.
CD01423-11-23-15
Setting Stop Block
3 - 1
Page 16
Set Up
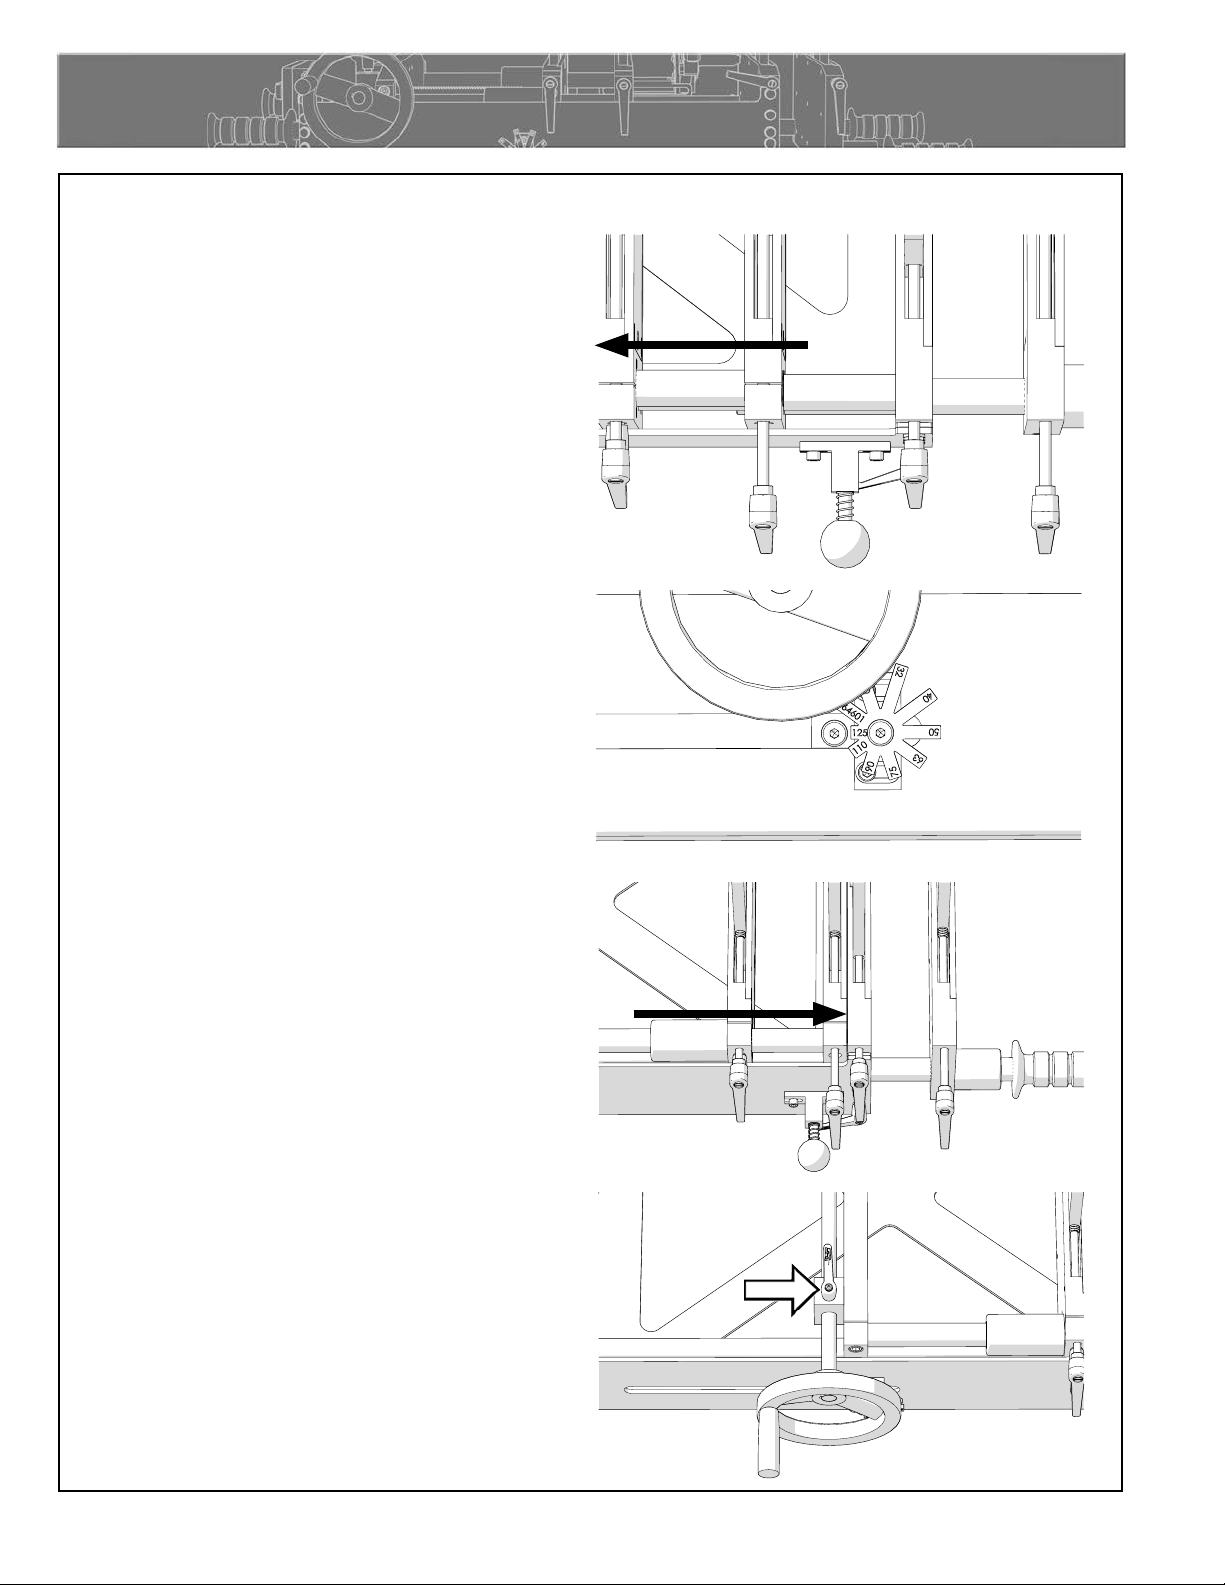
Set Up Calibration (continued)
Open movable jaws to release the setting stop.
Set the depth star to 125mm. The 125mm will point to the left
toward the bolt of the movable jaws.
CD01421-11-23-15CD01422-11-23-15CD01423-11-23-15
Close the movable carriage against the inner fixed jaw frame.
There should be no gap.
Lock the carriage.
CD01424-11-20-15
3 - 2
Page 17
Set Up
Set Up Calibration (continued)
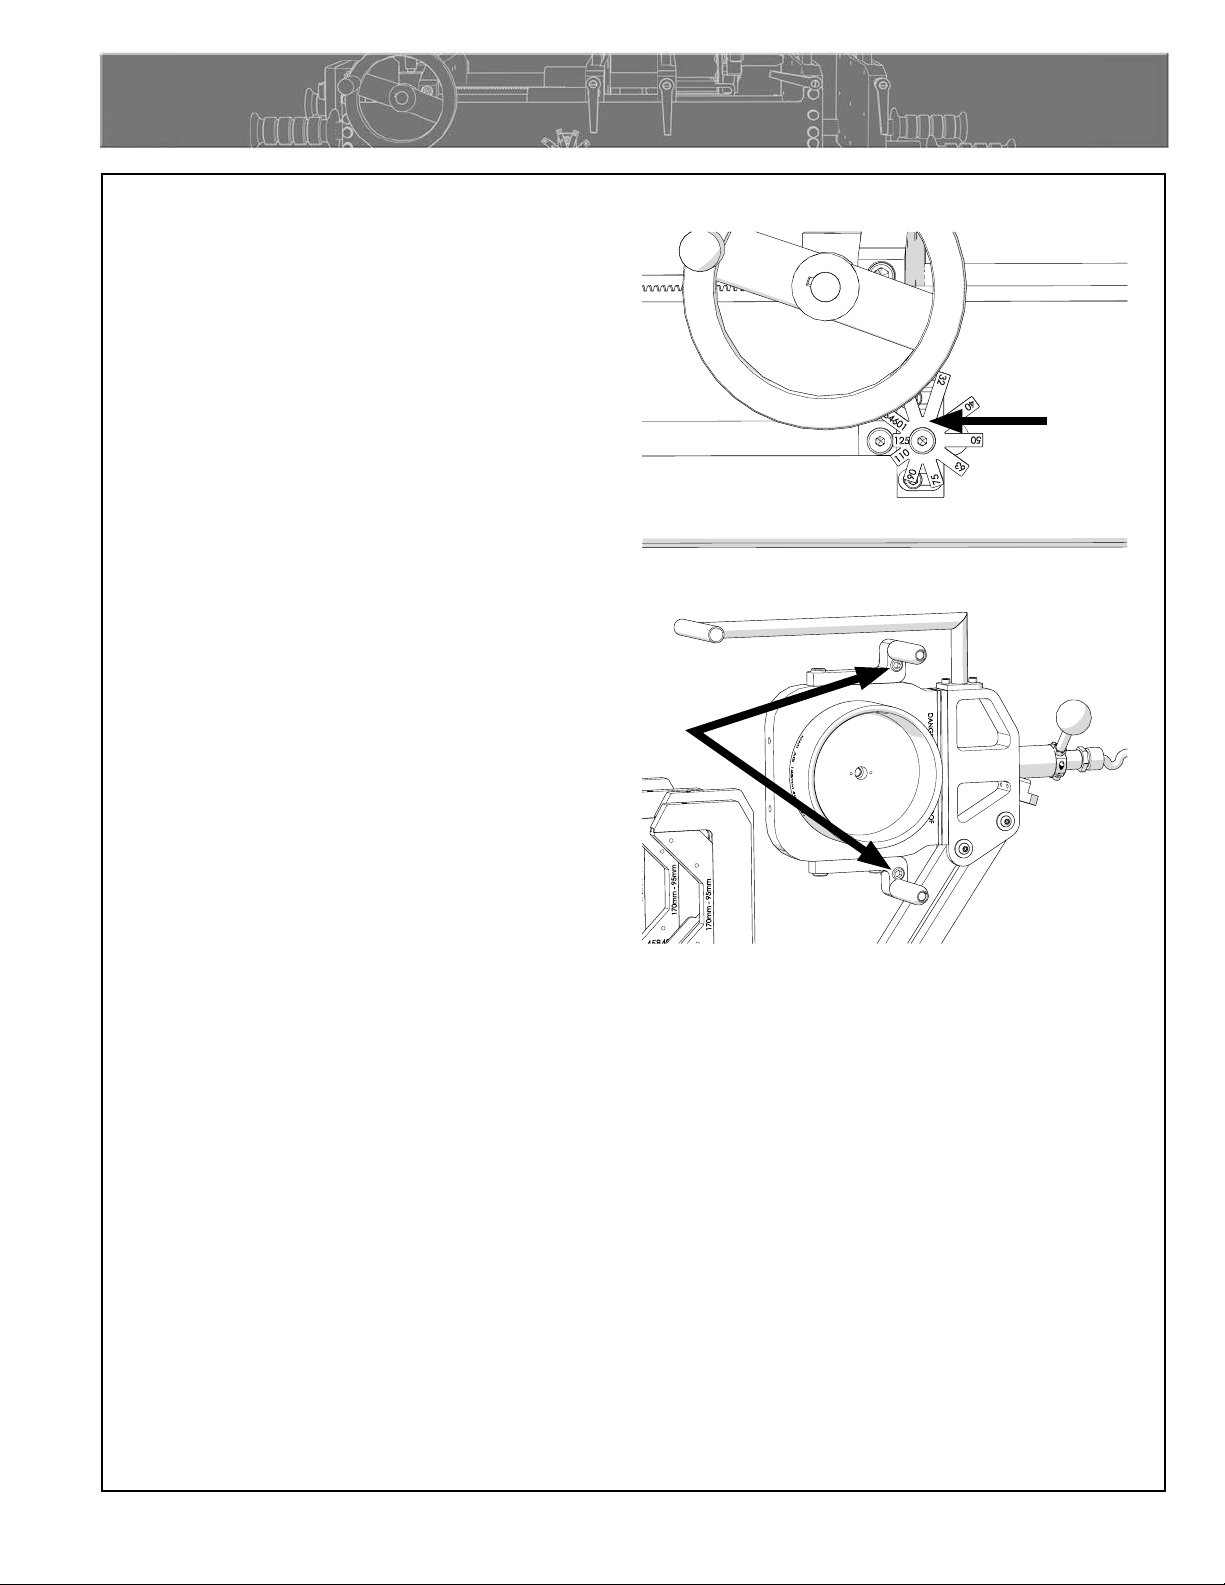
Slide the depth star block to the left until it contacts the bolt.
Tighten the bolts on the depth star block to lock the position.
Loosen the set screws for the short heater stop bolts.
CD01425-11-20-15CD01426-11-20-15
3 - 3
Page 18
Set Up
Set Up Calibration (continued)
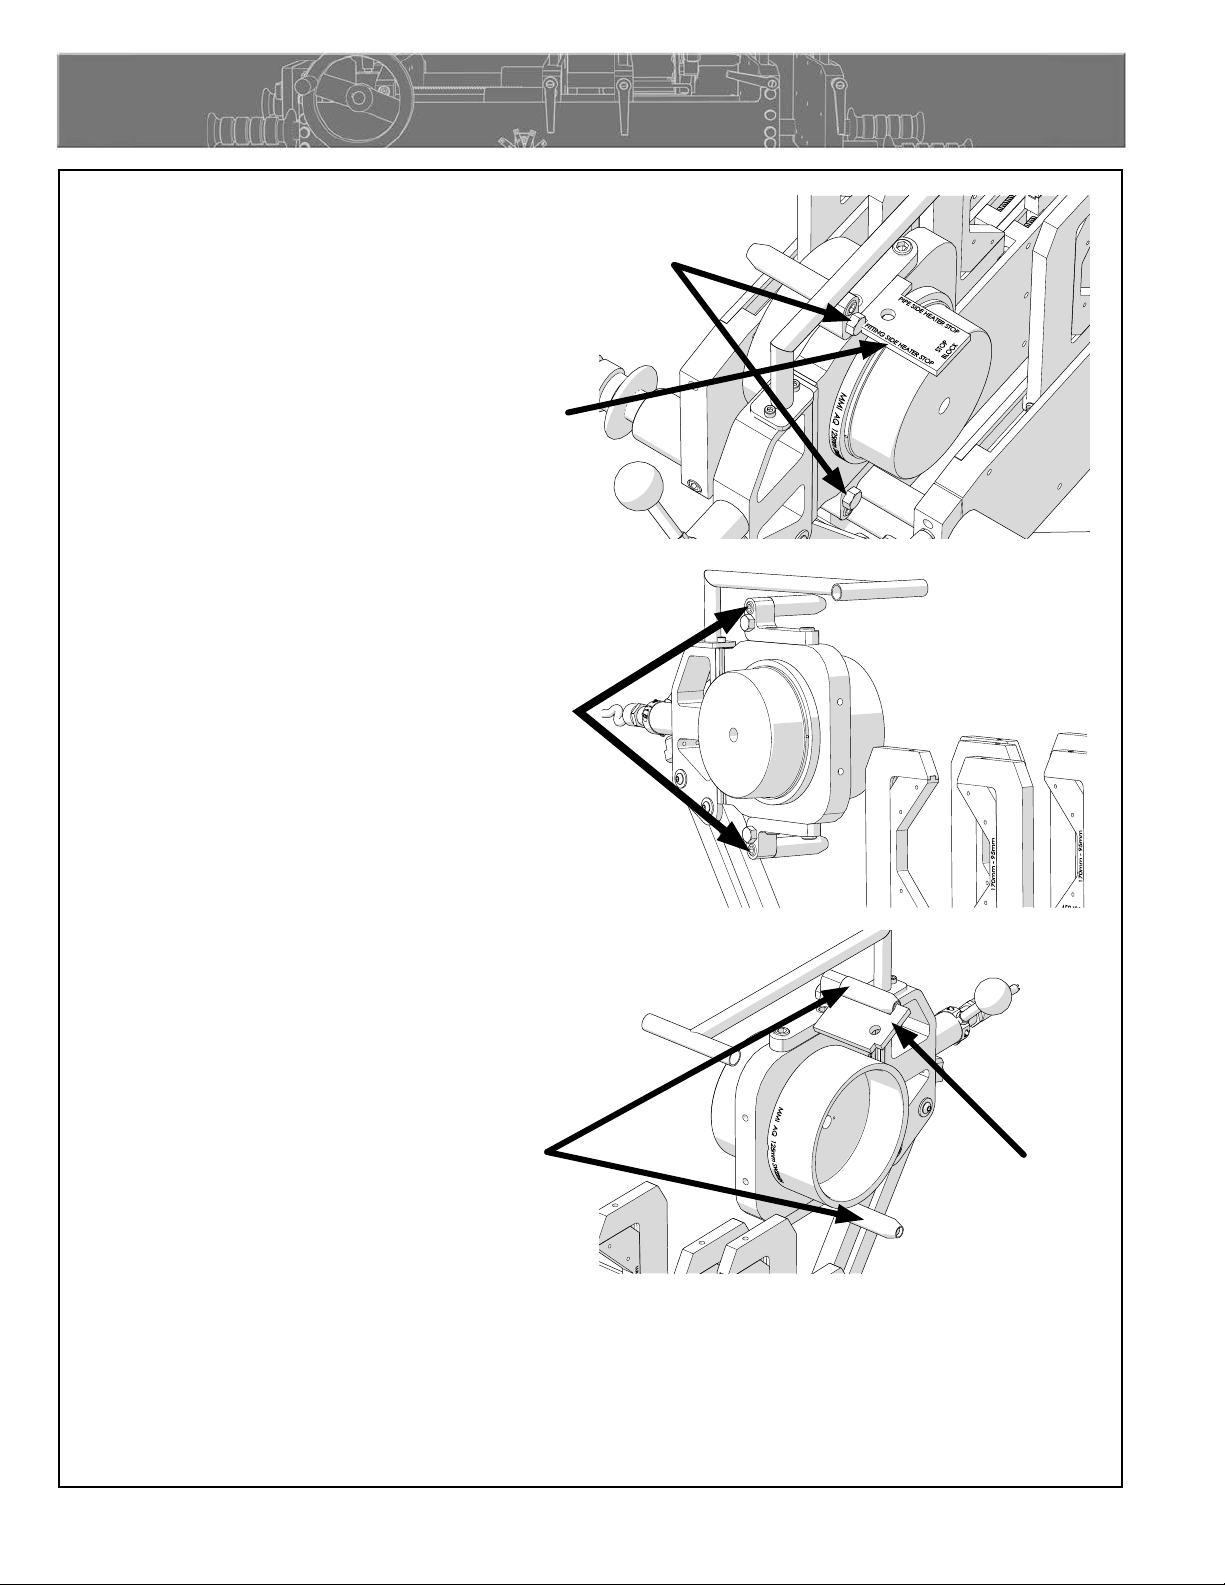
Insert the Set Up Gauge using the fitting side heater stop gauge
and adjust short heater stop bolt until the bolt touches the gauge
(from the heater stop mount) in both locations.
Tighten the set screws to lock the bolts in position.
Set Up Gauge
Loosen the set screws for the long heater stop bolts.
Short Heater
Stop Bolt
CD01427-11-20-15CD01428-11-20-15CD01429-11-20-15
Insert the Set Up Gauge using the pipe side heater stop gauge and
adjust long heater stop bolts until the bolt touches the gauge (from
the heater stop mount) in both locations.
Tighten the set screws to lock the bolts in position.
Long Heater
Stop Bolt
Set Up Gauge
3 - 4
Page 19
Set Up
Set Up Calibration (continued)
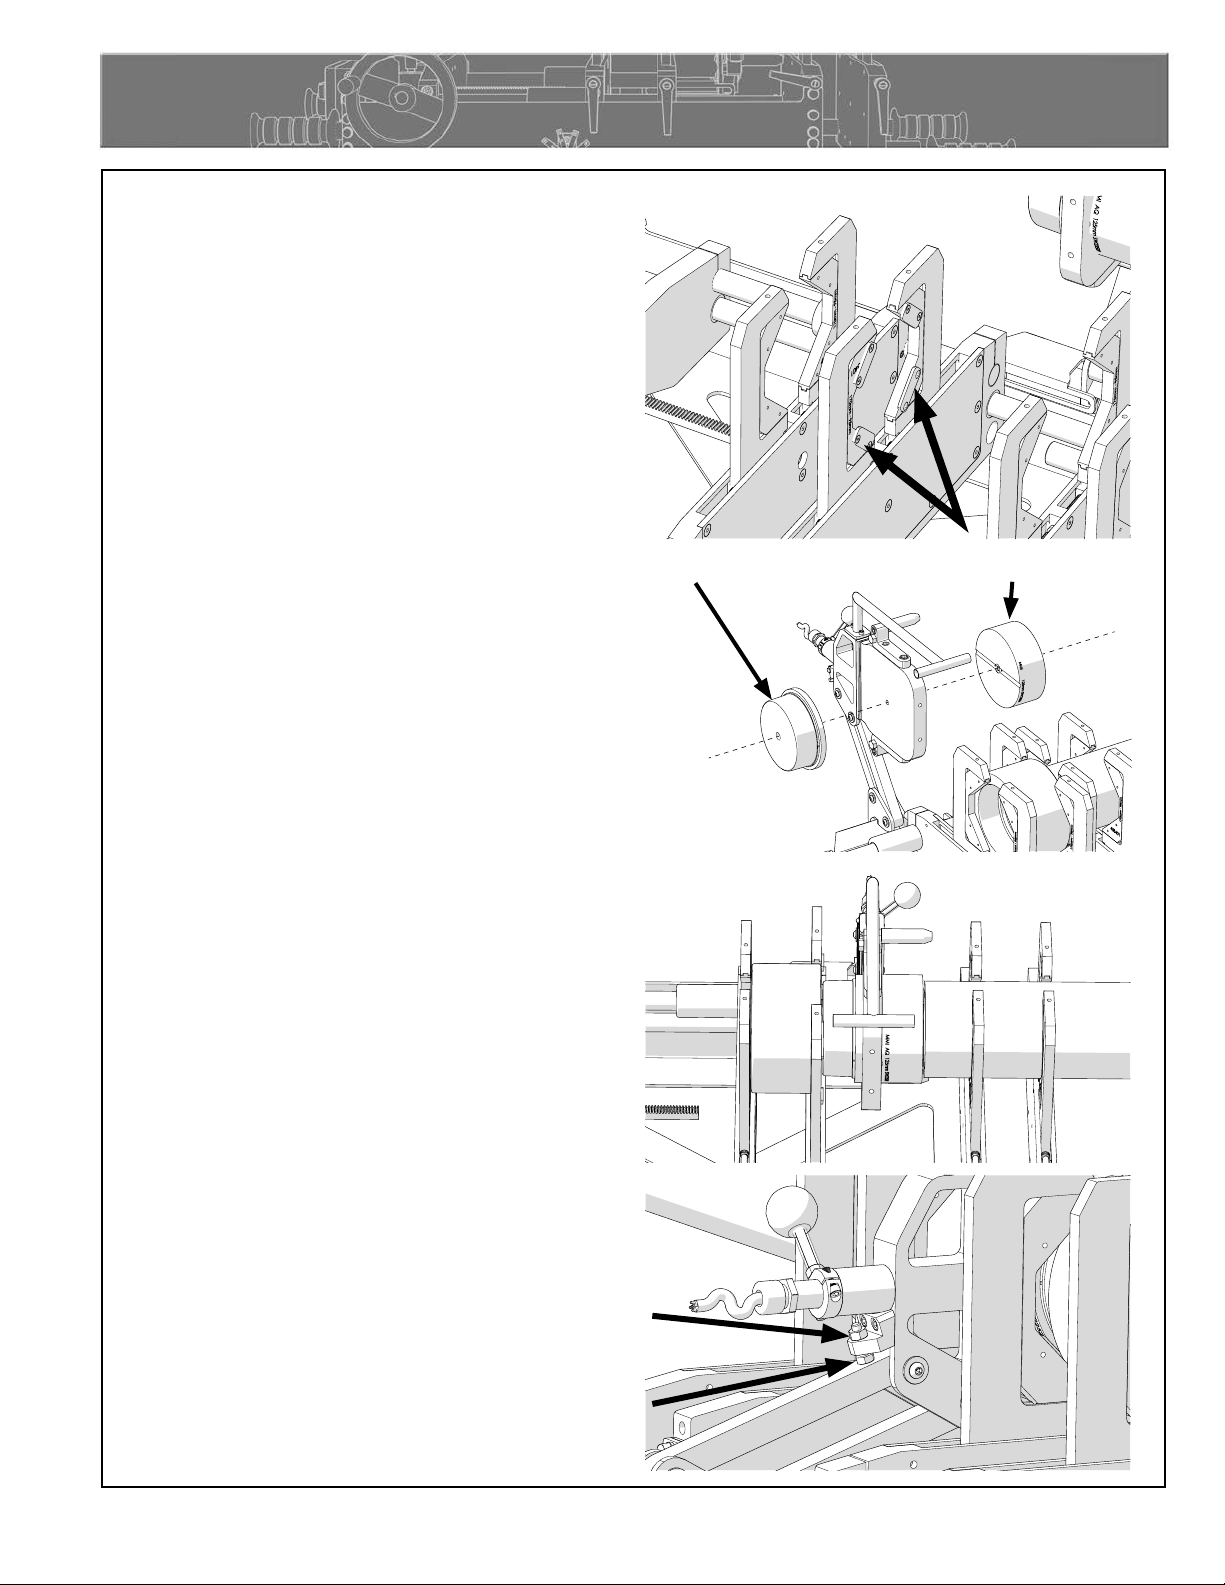
Select a fitting, the appropriate inserts and heater adapters to
match.
Install the heater adapters on the heater. The pipe heater adapter is
installed on the side of the heater with the long heater stops.
Install the inserts with the stops on the inner jaw frame.
CD01430-11-20-15CD01431-11-20-15CD01432-11-20-15
Fitting Heater Adapter
Install pipe and fitting into the machine. The fitting will be inserted
against the inserts with the stops on them.
Slowly advance the movable jaws until the fitting is close to the
heater adapter.
Pipe Heater Adapter
Using a 7/16" wrench, loosen the locking nut on the back of the
heater swivel assembly.
Adjust the center height of the heater to match the fitting to the
vertical alignment of the heater adapter.
Tighten the locking nut.
TX04857-03-14-16
3 - 5
Page 20
Fusion Procedure
Read Before Operating
Before operating this machine, please read this manual thoroughly, and
keep a copy with the machine for future reference.
When fusing thermoplastic pipe materials, refer to the pipe manufacturer's
suggested procedures or appropriate joining standard.
The pipe and fitting can be fused in either side of the machine removing
the need to reposition the machine.
TX04858-12-14-15
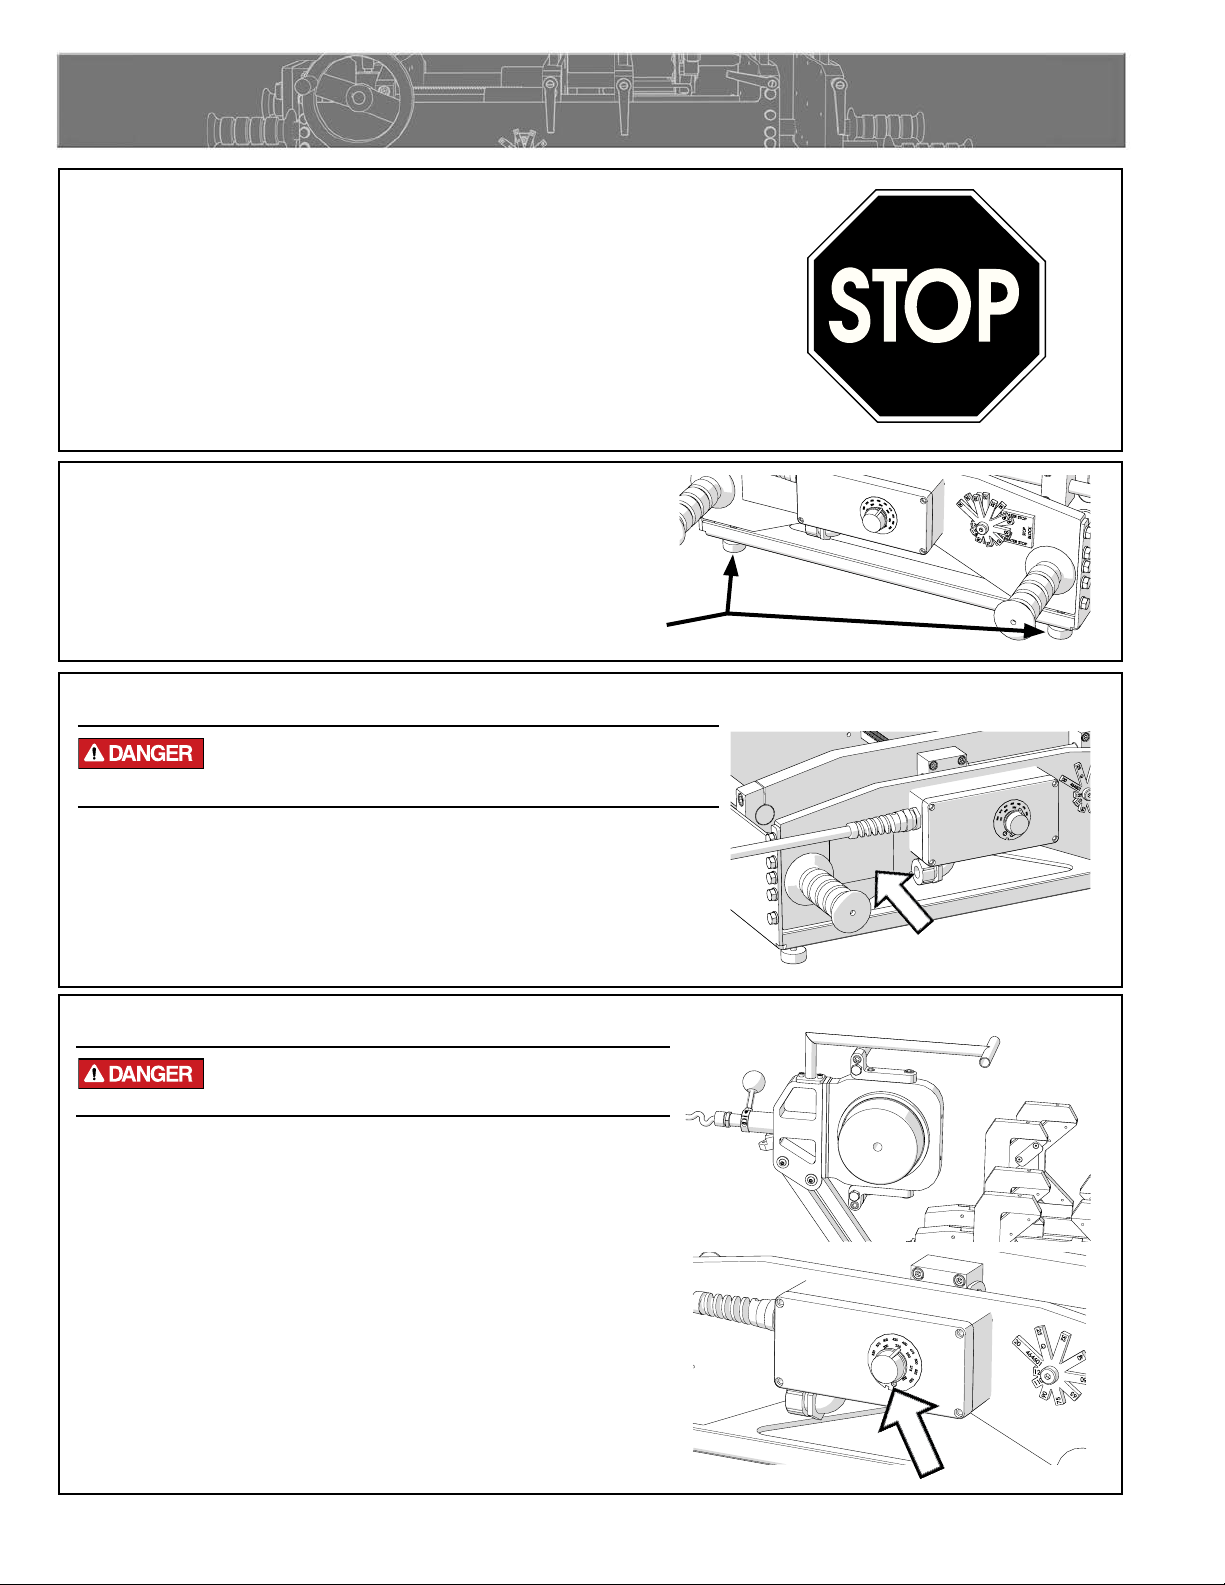
Level Machine
Use a torpedo level along the top of the jaw frames and adjust the
leveling legs
STOP-12-22-92
TX04859-12-14-15
Leveling legs
Connecting to Power
All electrical equipment and power sources must be located in a
non-explosive atmosphere. Failure to do so will result in serious
injury or death.
The heater must be connected to a source rated for the device's power
requirements. The device has a plate or label with the device's power requirements.
Consult generator sizing form in the back of this manual to determine the proper
size generator to power all electrical equipment.
TX04860-12-14-15
Prepare Heater
Heater is not explosion proof. Operation of heater in an
explosive atmosphere will result in serious injury or death.
Install socket fusion heater adapters if not already installed.
Ensure the pipe heater adapter goes on the side with the long heater stops.
NOTICE: The heater should never be used without socket fusion heater
adapters installed. Refer to the "Maintenance" section of this manual for
installation procedure.
Plug heater into a proper power source.
Allow heater to warm-up to operating temperature.
Refer to the "Maintenance" section of this manual for instructions on how
to adjust heater temperature.
CD01441-11-30-15 CD01456-12-10-15
CD01411-11-30-15
CD01440-11-23-15
TX04861-12-14-15
4 - 1
Page 21
Fusion Procedure
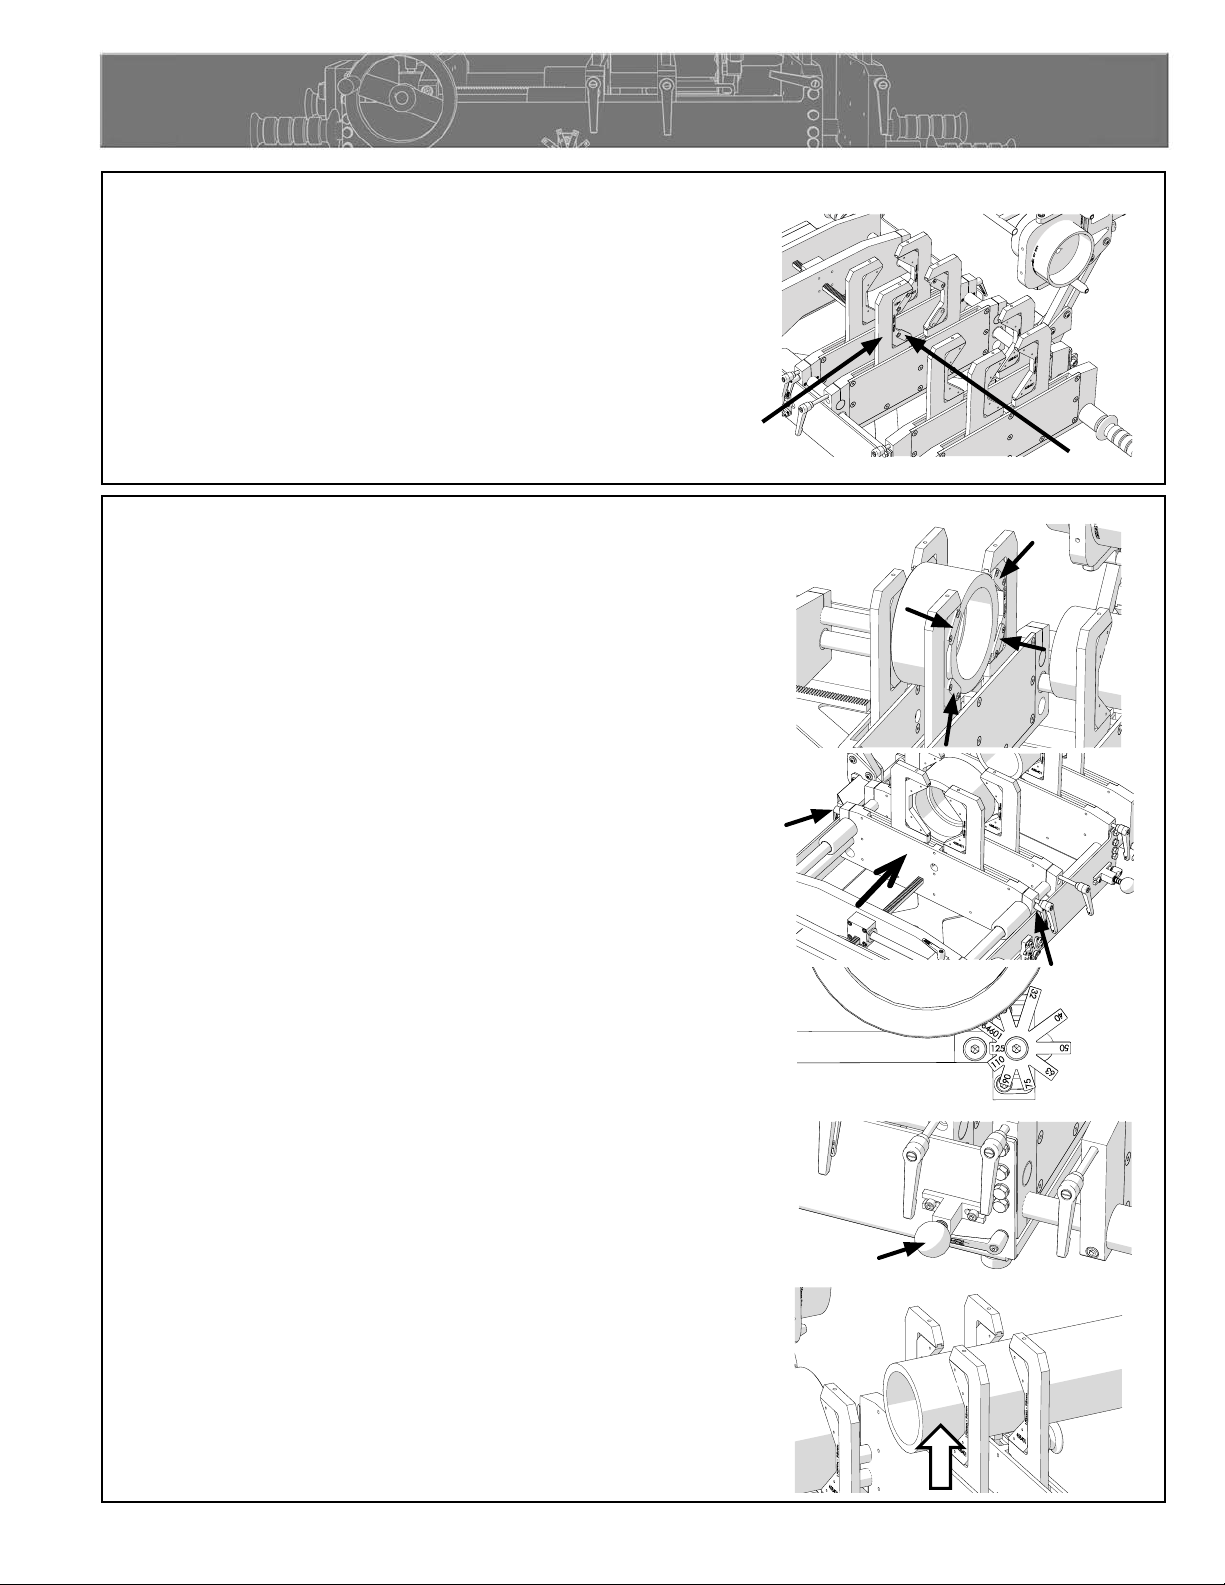
Install Inserts
Inserts are installed into the insert holders on each jaw frame.
Inserts are locked into place by a spring detent in the insert
holder. The inserts with the stop tabs are for the fitting and are
installed on the inner jaw frame on the same side as the fitting
heater adapter on the heater.
Install appropriate sized inserts for the pipe and fitting being
fused.
Insert Holder
TX04862-12-14-15
Load Pipe and Fitting
Load the fitting into the machine ensuring the fitting rests against the stop
tabs on the inner movable jaw. Clamp the inner movable jaw until the
fitting is firmly held in the jaw.
IMPORTANT: The jaws of the jaw frame can be used to back up the
fitting or use a clamped piece of pipe behind the fitting.
CD01398-10-5-15
Insert
CD01442-11-30-15
Rotate the depth star to the pipe size being fused. Press and hold in the
setting stop. Close the movable jaws against the setting stop. Release the
setting stop and lock the movable jaws. Load the pipe into the fixed jaws
of the machine. Move the pipe toward the fitting until the face of the pipe
is even with the face of the fitting. Clamp both jaws until the pipe is held
firmly in the jaws.
Unlock the movable jaws and open the carriage. The setting stop will
release.
The fitting and pipe must be clean and dry. Use a dry clean lint free nonsynthetic cloth to wipe the mating surfaces.
NOTICE: Do not touch fusion area with hands.
CD01444-11-30-15
CD01424-11-20-15
CD01420-11-23-15
CD01443-11-30-15
TX04863-12-14-15
4 - 2
Page 22
Fusion Procedure
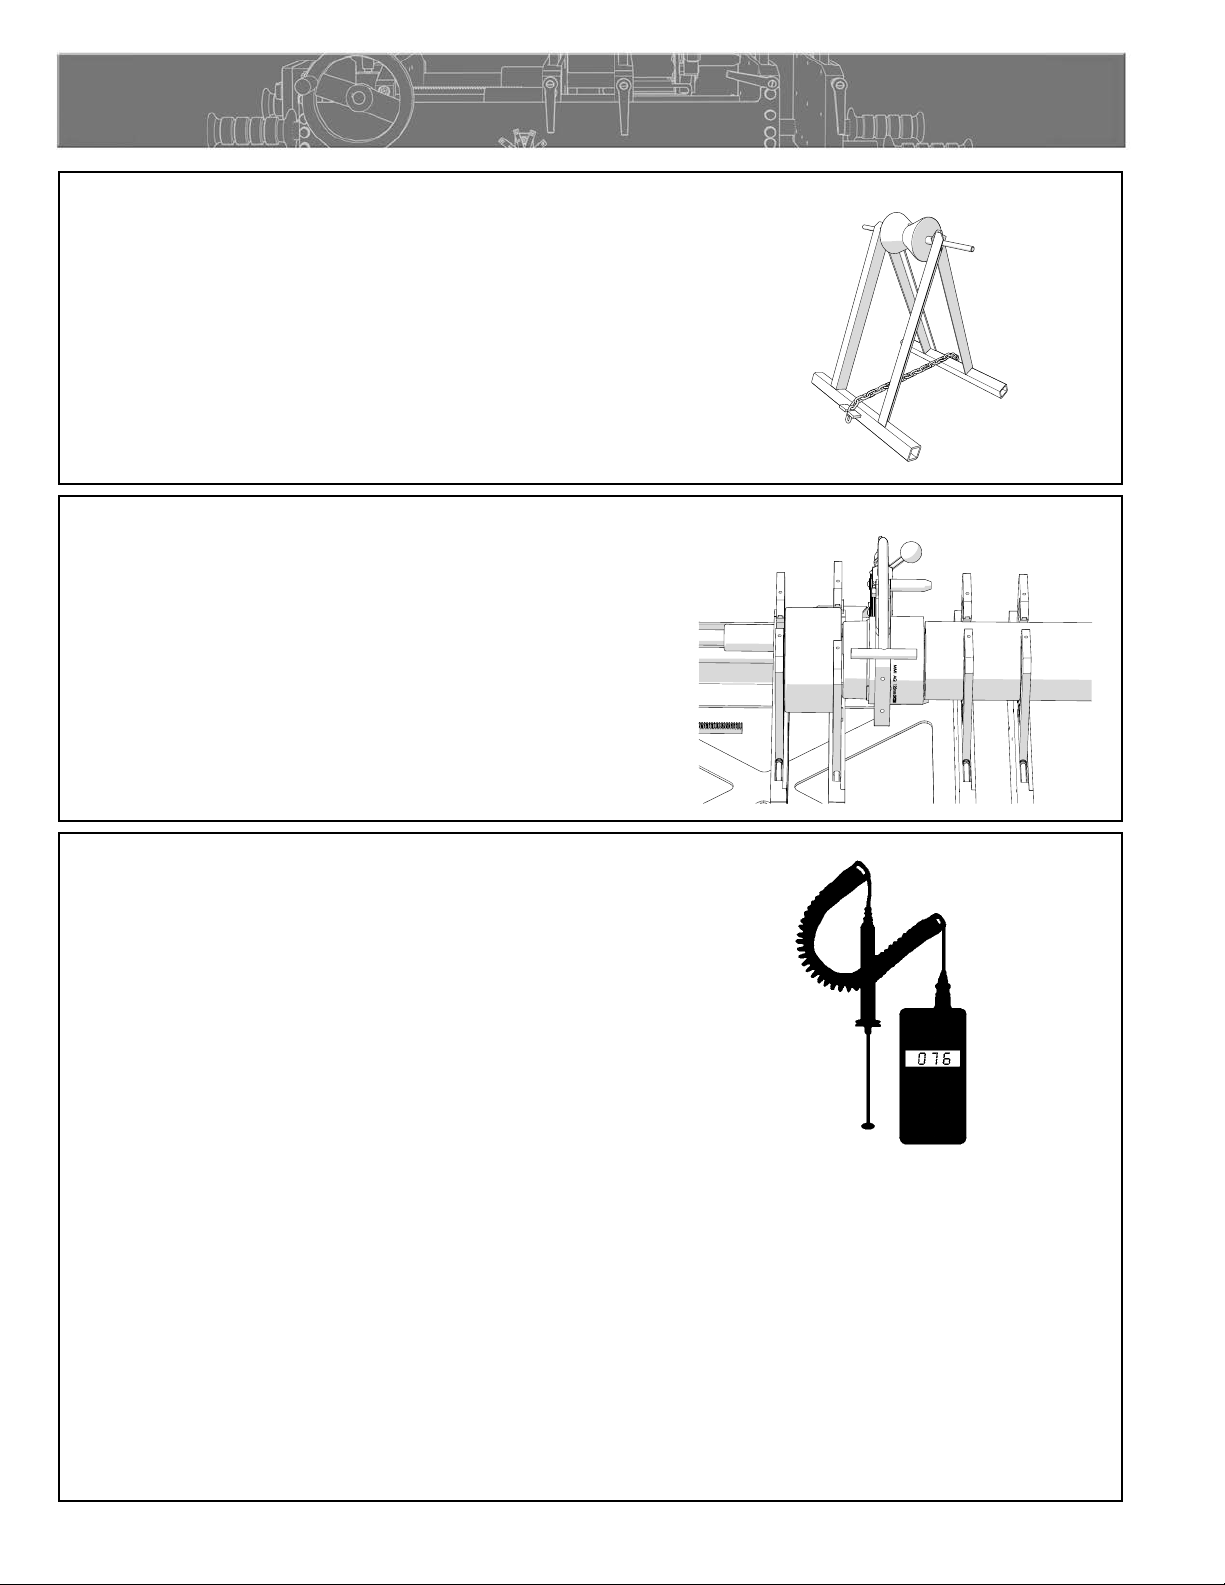
Support Pipe
Set up pipe stands and adjust height so the pipe is in line with the jaws of
the machine.
TX04864-12-14-15
Verify Alignment
Insert the heater between fitting and pipe.
Close the carriage until the fitting and pipe come close to the heater.
Verify the fitting and pipe are in proper alignment to the heater.
If not in proper alignment, perform the set up calibration again to align
machine.
Open the carriage.
CD01450-12-01-15
CD01431-11-20-15
TX04865-12-14-15
Check Heater Temperature
NOTICE: Incorrect heating temperature can result in questionable
fusion joints. Check heater adapters periodically with a pyrometer
and make necessary adjustments.
Refer to the "Maintenance" section of this manual for instructions on how
to adjust heater temperature.
Check heater surface temperature with a pyrometer.
Refer to the pipe manufacturer's recommendations or appropriate joining
standard for proper heater temperature.
Use a clean dry lint free non-synthetic cloth to clean the socket fusion
heater adapter surfaces.
WR00077-4-16-93
TX04866-12-14-15
4 - 3
Page 23
Fusion Procedure
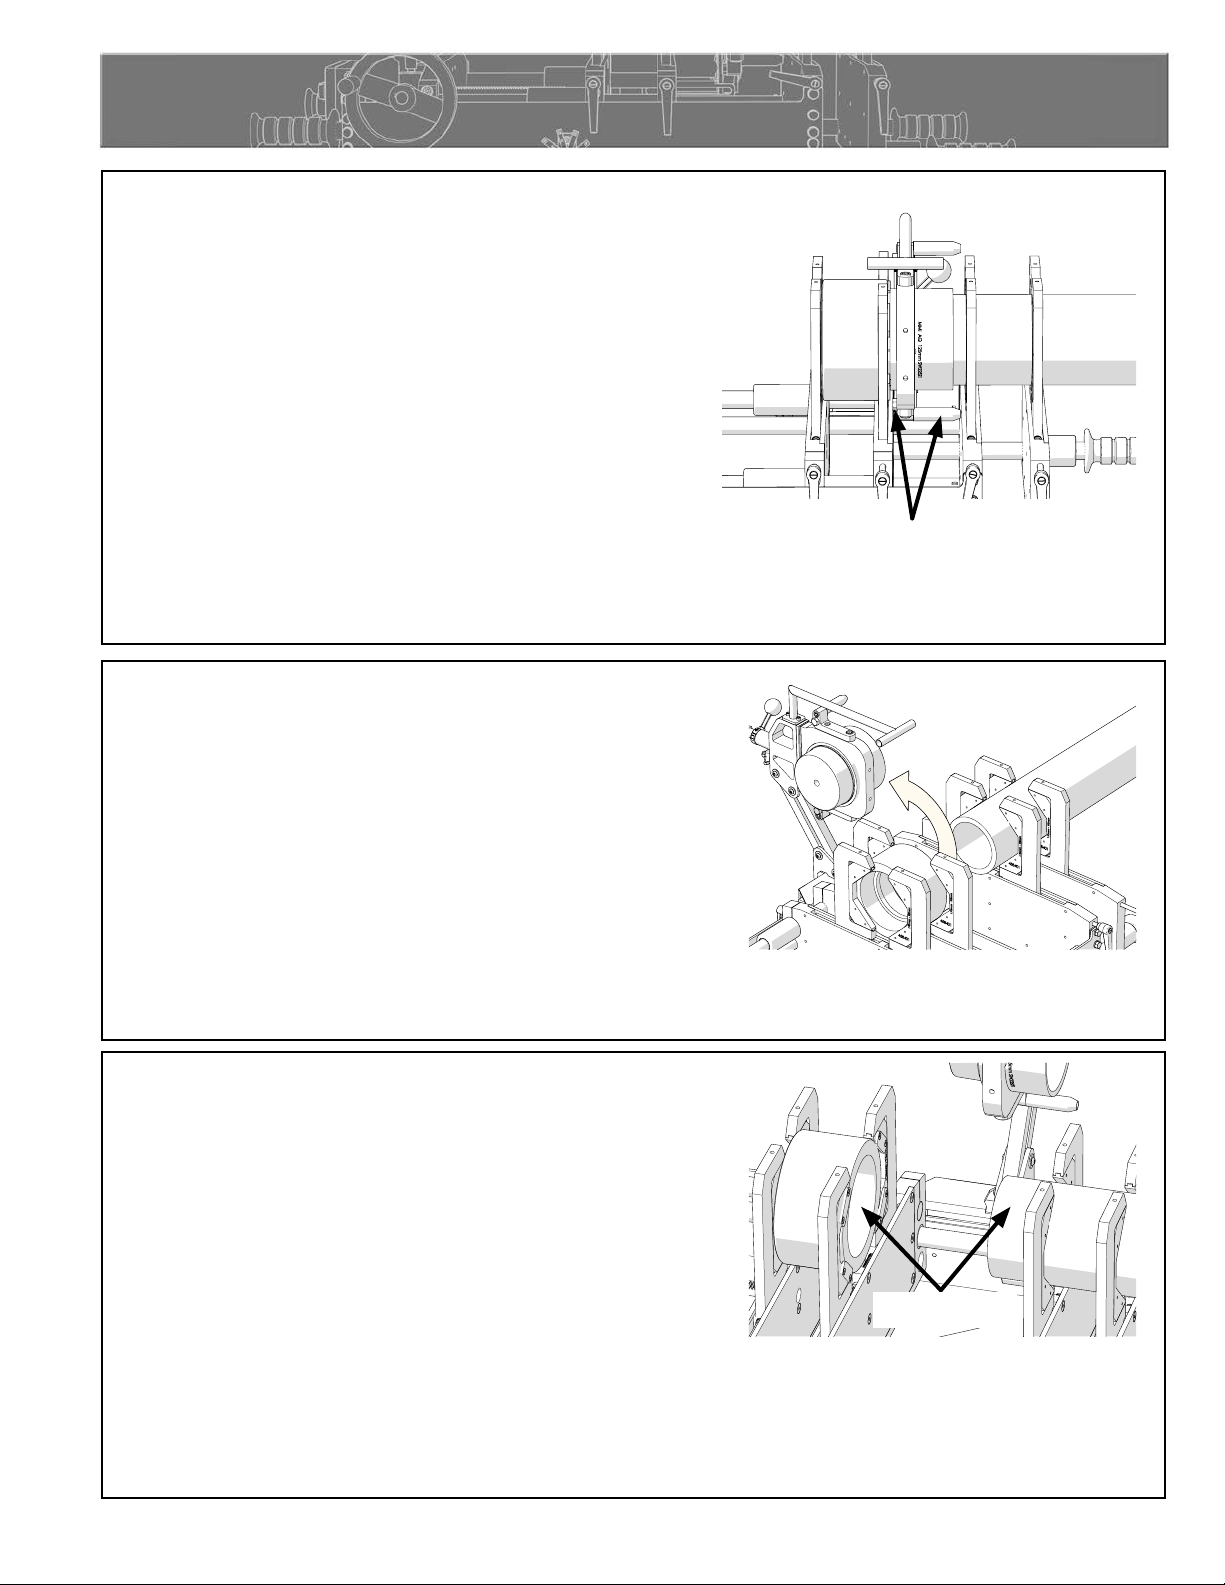
Heating the Pipe and Fitting
Close the carriage until the heater stops make contact with the jaw frames.
IMPORTANT: Do not force the pipe and fitting onto the heater. Allow the
pipe and fitting to melt onto the heater. Forcing the pipe and fitting onto
the heater will damage the machine or create a questionable melt pattern.
Heating time starts when the pipe and fitting are fully inserted onto the
heater adapters.
Heat the fitting and pipe for the pipe manufacturer or joining standard's
specified period of time.
TX04867-12-14-15
CD01446-12-01-15CD01447-12-01-15CD01448-12-01-15
Heater Stops
Remove Heater
Open the carriage completely. Quickly retract the heater.
TX04868-12-14-15
Inspect Melt
Quickly inspect the heated parts to make sure all surfaces have
been melted properly.
If melt is not complete, cut off melted pipe end. Use a new fitting
and repeat preparation and heating process.
TX04869-12-14-15
Inspect Melt
4 - 4
Page 24
Fusion Procedure
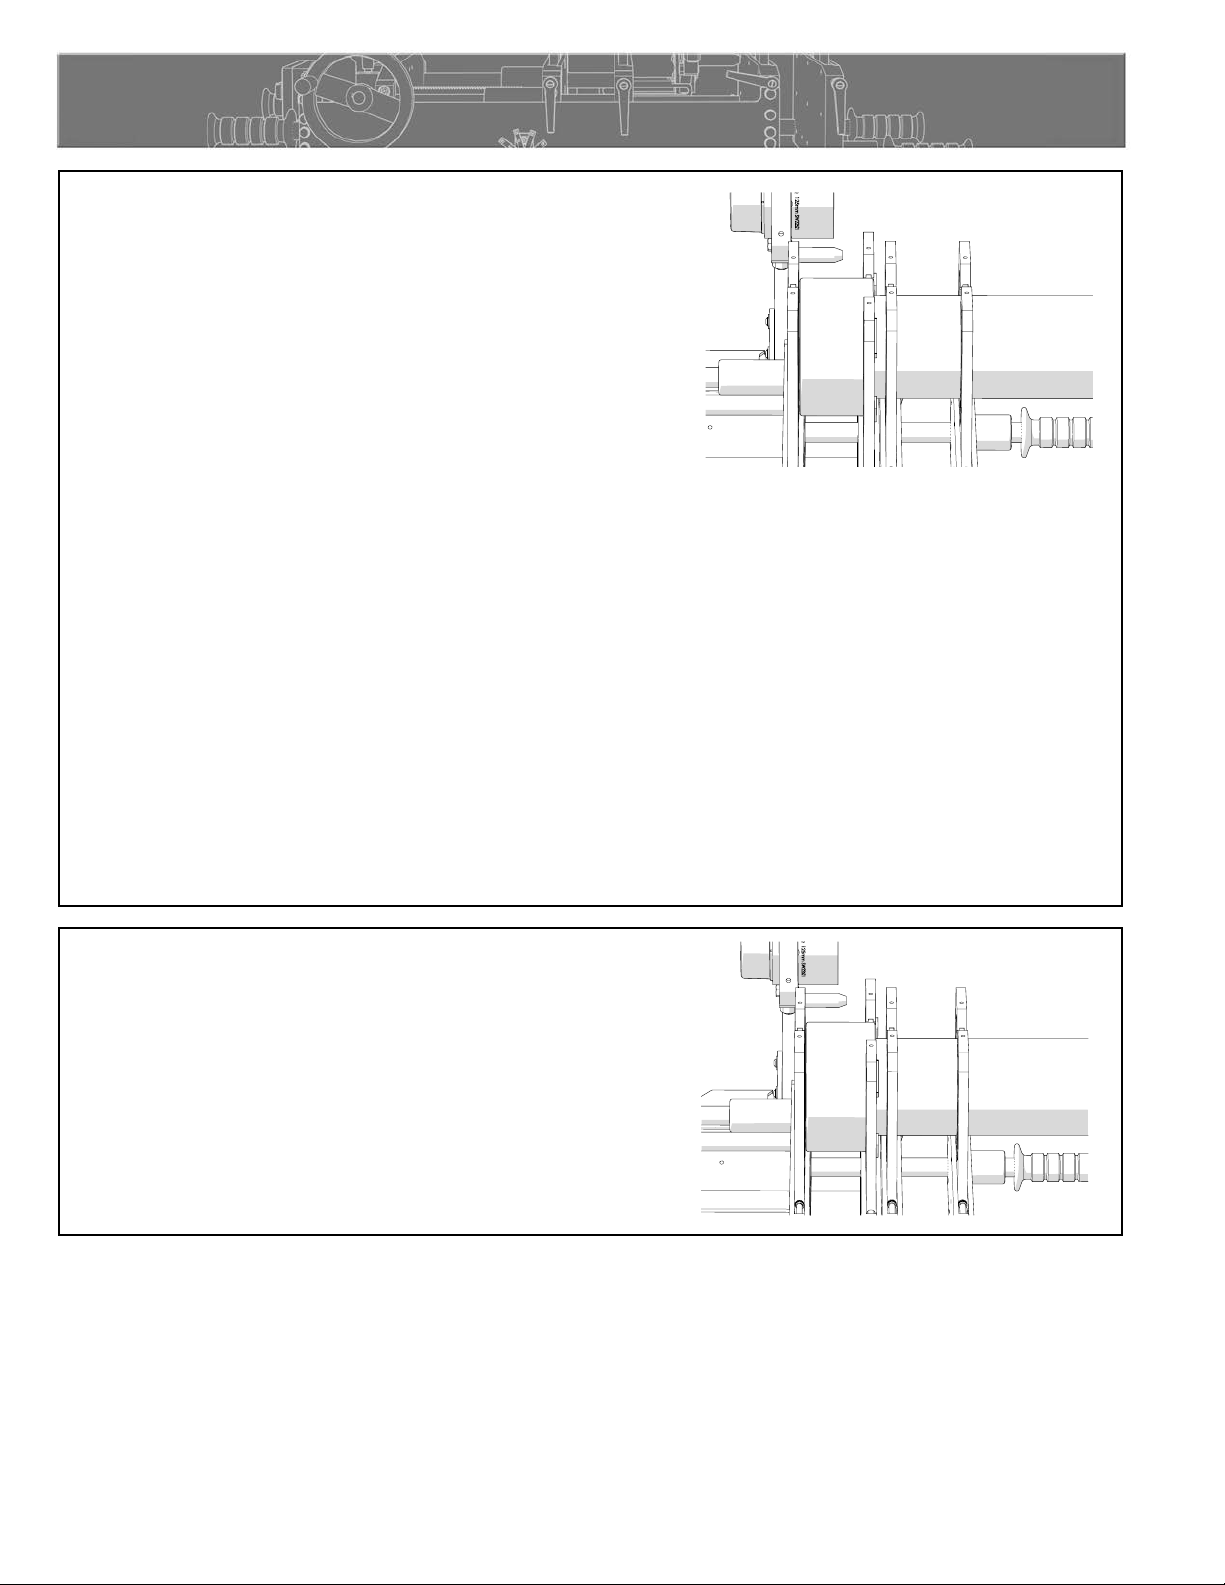
Fusion and Cooling
Close the carriage until the carriage stops against the depth star.
NOTICE: Be sure to complete the joint in the time allowed by the
pipe manufacturer or appropriate joining standard.
Lock the carriage. Allow the carriage to stay in place for the total
cooling time specified by the pipe manufacturer or appropriate
joining standard.
After the cooling time, if you are not satisfied with the results of
the fusion there are adjustments that can be made to improve the
fusion.
1) If the melt is not reaching the insertion depth mark on the
pipe, then shorten the length of the long heater stops.
2) If there is too much melt or the melt is exceeding the
insertion depth mark on the pipe, then lengthen the long
heater stops.
IMPORTANT: Use the Set Up Calibration procedure as the base
set up before making adjustments to the machine stops.
CD01449-12-01-15
TX04870-12-14-15
Opening Jaws
After the joint has cooled for the pipe manufacturer's recommended time
or appropriate joining standard, loosen all clamp handles, and remove the
fused pipe and fitting.
Open the movable jaws.
TX04871-12-14-15
CD01342-10-5-15
4 - 5
Page 25
Maintenance
Preventative Maintenance
To insure optimum performance, the machine must be kept clean and well
maintained.
With reasonable care, this machine will give years of service. Therefore, it
is important that a regular schedule of preventive maintenance be kept.
Store machine inside, out of the weather, whenever possible.
TX00428-8-10-95
Cleaning the Machine
The machine should be cleaned by using compressed air to blow away
debris and wiped clean with a clean rag.
CD00142-11-2-94
CD01407-11-12-15
TX04872-12-14-15
Clean Jaws and Inserts
To prevent slippage and insure proper alignment, the jaws and inserts must
be clean. Clean the jaws and inserts of any dirt or residual material using
a stiff-bristled brush.
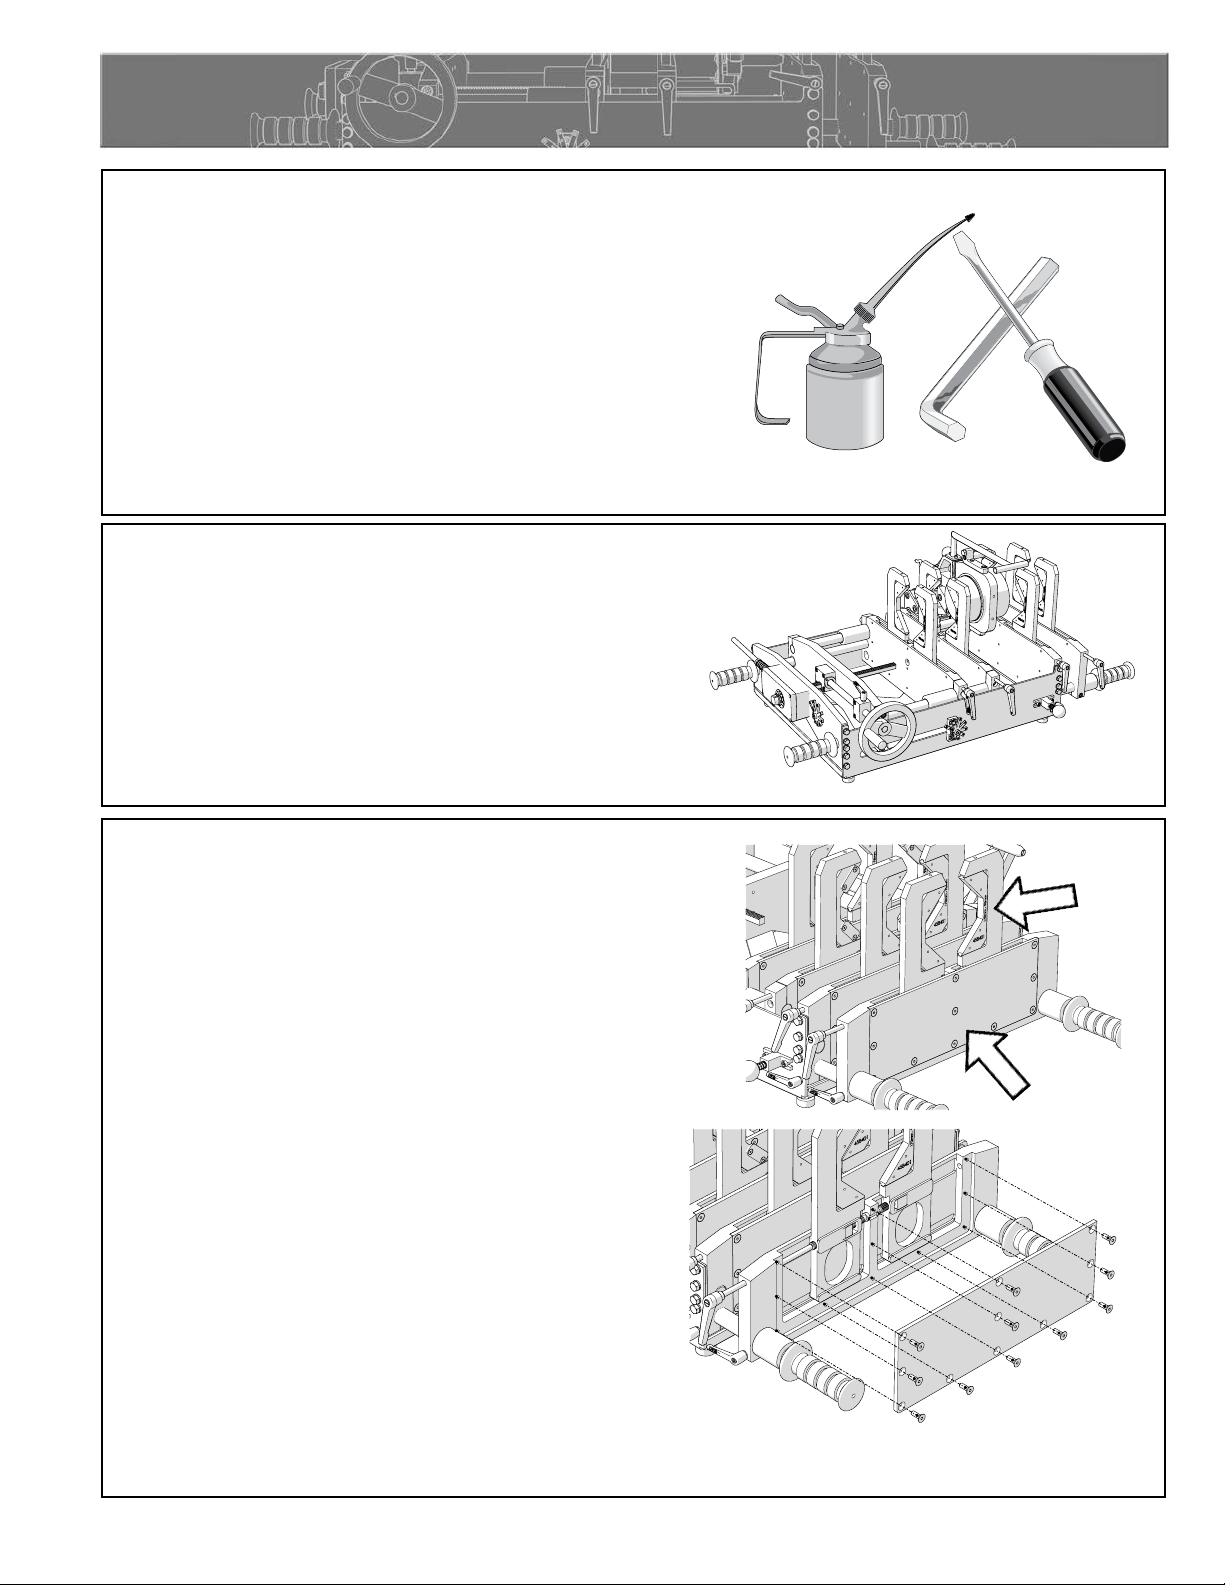
If the jaws become hard to open and close, the jaw frame can be
disassembled so it may be cleaned and lubricated.
Clean the jaw frame of any old lubrication and inspect internal parts for
damage. Alcohol can be used to remove the old lubrication. Apply dry
moly lubricant to the friction surfaces of the inside of the jaw frame. Allow
the lubricant to dry. Re-assemble the jaw frame. Repeat for the additional
jaw frames.
CD01395-10-5-15CD01461-15-10-15
TX04873-12-14-15
5 - 1
Page 26
Maintenance
Fasteners Must Be Tight
Check all nuts, bolts, and snap rings to make certain they are secure and
in place.
TX00437-9-13-94
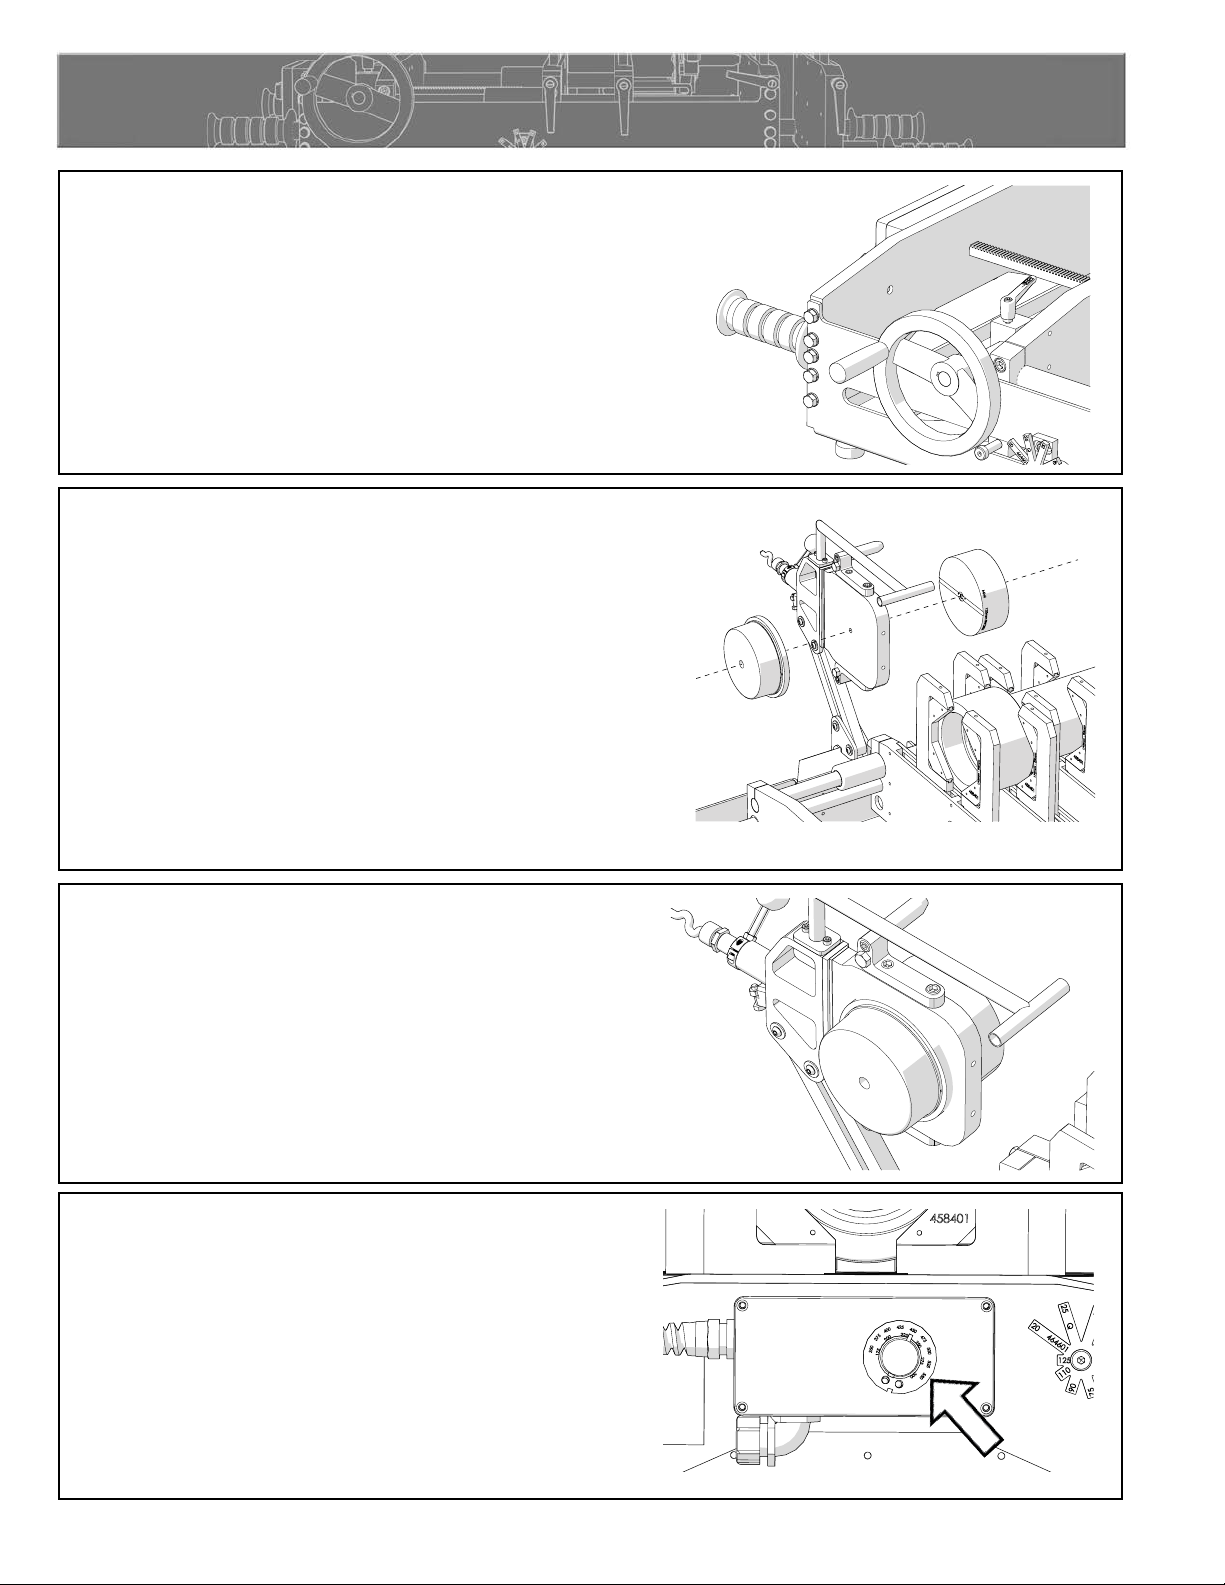
Installing Socket Fusion Adapters
The heater body of this assembly is not coated. Coated socket fusion heater
adapters are available for all socket fusion applications.
Care should be taken to ensure that the socket fusion heater adapters are
seated on the heater body, and that there is no foreign matter trapped
between these surfaces.
IMPORTANT: Do not over tighten the bolts.
The surfaces of the socket fusion heater adapters are coated with an antistick
coating.
Ensure the pipe heater adapter is installed on the side of the heater with the
long heater stops.
TX04874-12-14-15
CD01454-12-01-15
CD01452-12-01-15CD01453-12-01-15
Clean Heater Surfaces
The heater adapters must be kept clean and free of any plastic build up or
contamination.
Before each fusion joint the heater surfaces must be wiped with a clean dry
lint free non-synthetic cloth.
NOTICE: Do not use an abrasive pad or steel wool. Use a non-synthetic
cloth that won't damage surfaces.
TX04879-12-14-15
Adjusting Heater Temperature
Turn knob to desired temperature. Measure the heater surface
temperature with a pyrometer. Any variance must be corrected to the
pyrometer reading.
Loosen setscrew in the knob. Turn knob to point to the same temperature
as the pyrometer. Tighten setscrew in the knob.
Turn knob to desired temperature. Allow heater to stabilize at the new
temperature (5 to 10 minutes) after adjusting. Verify the temperature.
TX04875-12-14-15
CD01451-12-01-15
5 - 2
Page 27
Maintenance
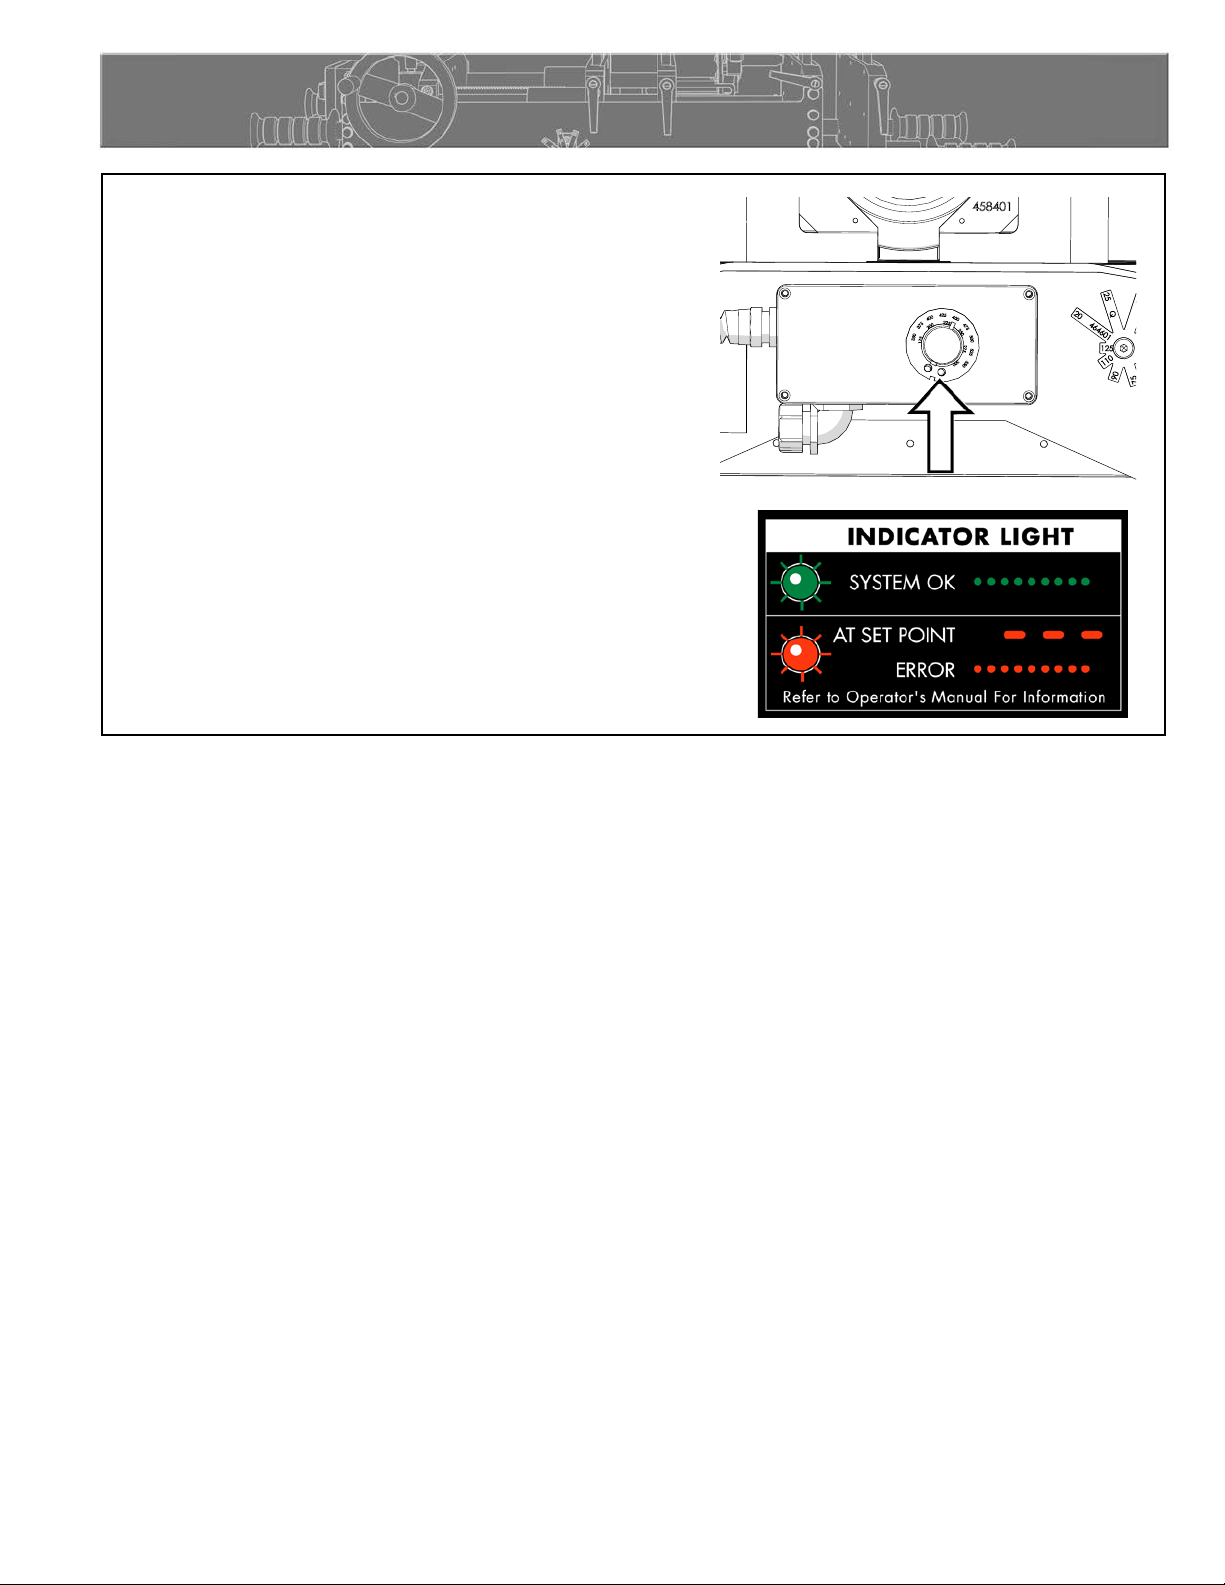
Heater Indicator Light
The heater has a green indicator light which will flash on and off. This
indicates that the controller is operating normally. If the green indicator is
not flashing then the controller may not be operating properly. If this occurs,
disconnect power and have the heater repaired by an McElroy Authorized
Service Center.
The heater has a red indicator light at the bottom of the temperature scale.
When the heater is plugged in and preheating the red light glows steadily
until the set temperature is reached. The red light then goes off and on as
the heater maintains temperature.
If the heater is not operating properly, the control will attempt to turn
the heater off and the red indicator light will flash rapidly. If this occurs,
disconnect the power and take it to a McElroy Authorized Service Center for
repair.
TX04876-12-14-15
CD01451-12-01-15
PH02571-09-16-03
5 - 3
Page 28
Maintenance Checklist
Fusion Machine Checklist
Item to Check Satisfactory Needs Repair Comments
Repair
UNIT
Machine is clean
All nuts and bolts are tight
All placards and handles are in place
All clamp handles turn freely
Cords and plugs are in good condition
Hand wheel for movable jaws turns freely
Jaws are properly aligned
Inserts fit properly
Depth stars are in place and not damaged
Heater moves in and out of the carriage freely
Heater adapters clean and in good condition
Surface temperature checked with pyrometer
Set Up Gauge in place and not damaged
Heater rotates and locks properly
Rack is clean and in good condition
TX04877-12-14-15
6 - 1
Page 29
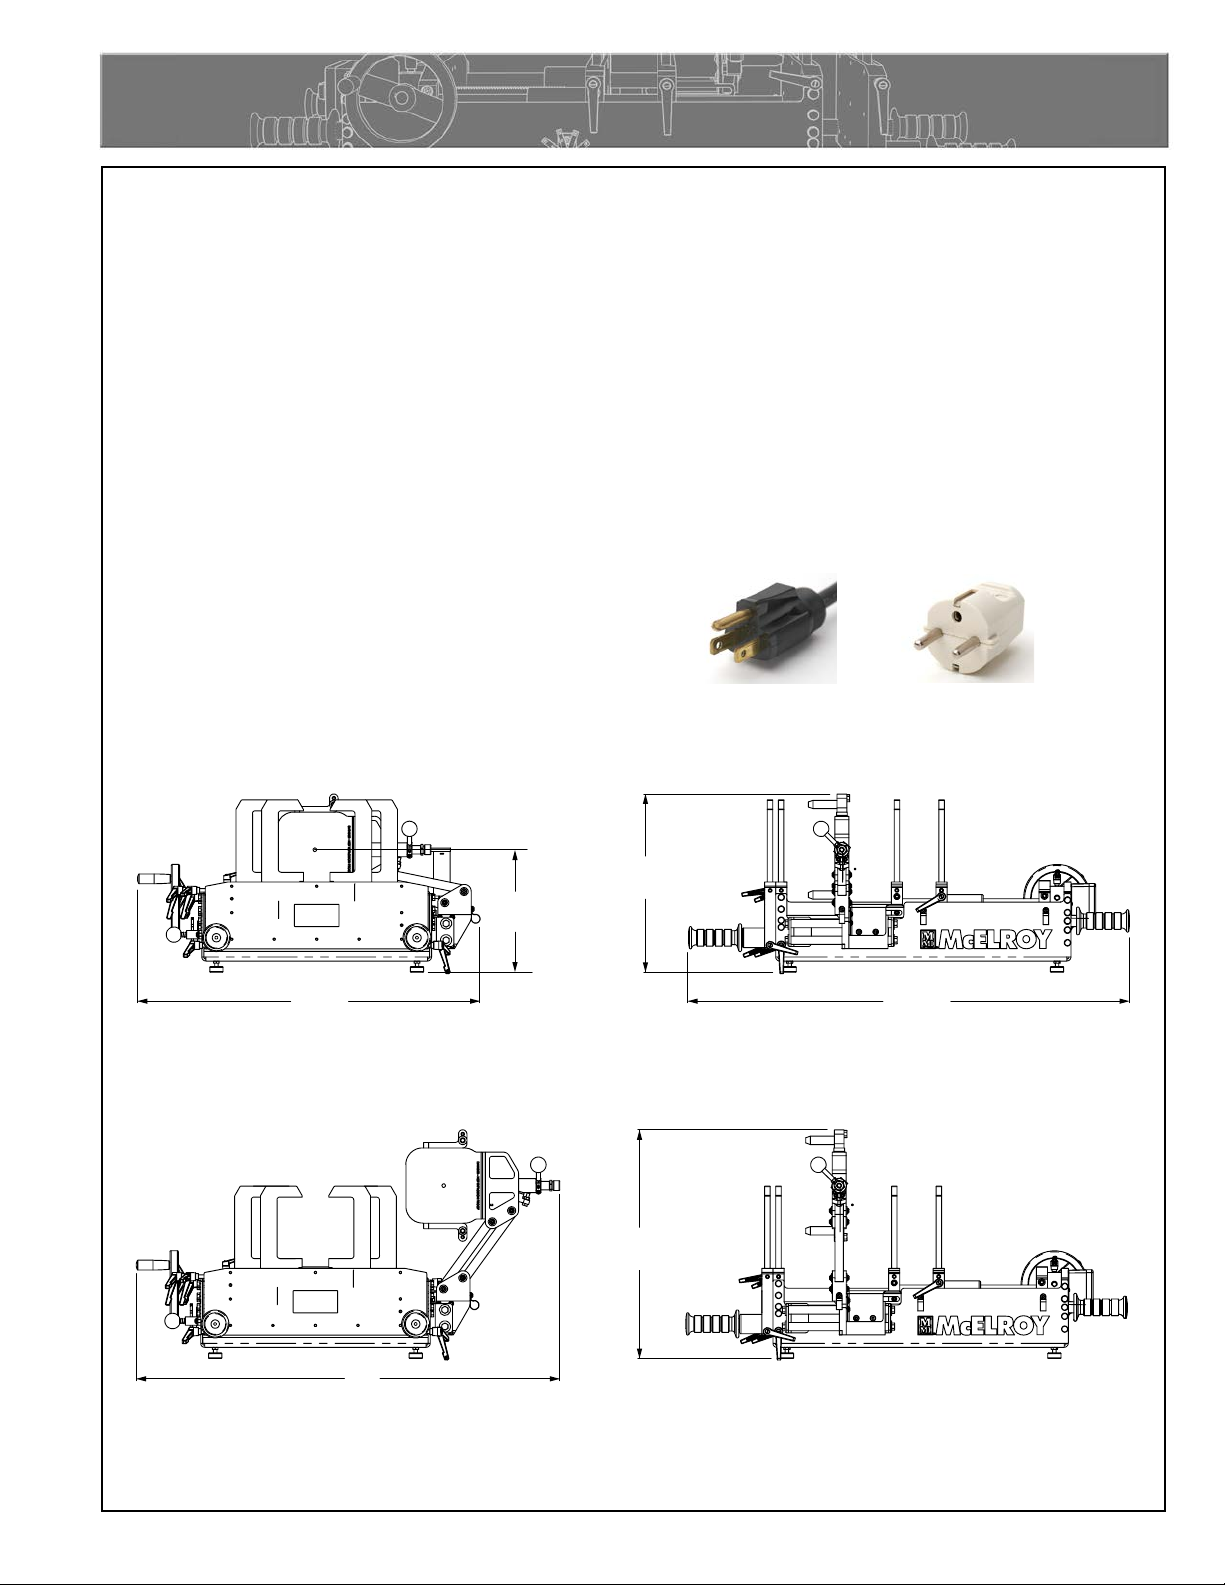
Specifications
20.5"
521mm
16"
406mm
38"
965mm
40.1"
1019mm
20.5"
521mm
20.5"
521mm
Fusion Machine Specifications: SmartFab™ 125
Dimensions:
Length: 40.1" (1019mm)
Width: 30.8" (782mm)
with Heater Extended: 38" (965mm)
Height: 16" (406mm)
with Heater Extended: 20.5" (521mm)
Weight:
Carriage Assembly: 145 lbs (65.8Kg)
Power Requirements:
Heater: 1600W, 100-120V, 14.5A, 50/60Hz, 1Ph
1600W, 200-240V, 6.7A, 50/60Hz, 1Ph
Plug Type: A) NEMA 5-15P, 15A, 2 Pole, 3 Wire
M) DIN 49441, 16A, 2 Pole, 3 Wire
30.8"
782mm
11"
279mm
A M
16"
406mm
40.1"
1019mm
20.5"
521mm
TX04878-12-14-15
38"
965mm
Heater Extended
7 - 1
Page 30
Page 31
About this manual . . .
McElroy Manufacturing continually strives to give customers the best quality products available. This
manual is printed with materials made for durable applications and harsh environments.
This manual is waterproof, tear resistant, grease resistant, abrasion resistant and the bonding quality of the
printing ensures a readable, durable product.
The material does not contain any cellulose based materials and does not contribute to the harvesting of
our forests, or ozone-depleting constituents. This manual can be safely disposed of in a landfill and will
not leach into ground water.
TX001660-8-19-99
Page 32
 Loading...