

Page 1
PROOF
Content Type: Standard Color
Paper Type: STCO19 (Standard 50 White)
Page Count: 90
File type: Internal
Page 2
PROOF
Page 3
LulzBot TAZ User Manual
Aleph Objects, Inc.
PROOF
Page 4
LulzBot®TAZ 6 User Manual
by Aleph Objects, Inc.
Copyright © 2016 Aleph Objects, Inc.
Permission is granted to copy, distribute and/or modify this document
under the terms of the Creative Commons Attribution 4.0 International
Public License (CC BY-SA 4.0).
Published by Aleph Objects, Inc., 626 West 66th Street, Loveland, Colorado,
80538 USA.
For more information, call +1-970-377-1111 or go to LulzBot.com and
AlephObjects.com.
ISBN: 978-0-9893784-8-2 6.0-20160322
PROOF
Page 5
Contents
WARNINGS
Safety Information · · · · · · · · vii
Read Me First! · · · · · · · · · · · · · · · · viii
Hazards and Warnings · · · · · · · · · · · · · viii
Regulatory Compliance Statement Class B · · · · · ix
1 3D Printer Software · · · · · · · 11
1.1 Software Overview · · · · · · · · · · · · · 12
1.2 Software Types · · · · · · · · · · · · · · 12
1.3 Installing Drivers · · · · · · · · · · · · 13
1.4 CAD and 3D Modeling Software · · · · · · · · 13
1.5 Alternative Printer Host Software · · · · · · 14
2 Cura LulzBot Edition · · · · · · · 17
2.1 Cura · · · · · · · · · · · · · · · · · · 18
2.2 Quick Print Settings · · · · · · · · · · · 19
2.3 View Options · · · · · · · · · · · · · · · 23
2.4 Starting Your First Print · · · · · · · · · 27
2.5 Removing Your First Print · · · · · · · · · 30
2.6 Full Settings · · · · · · · · · · · · · · 31
2.7 Basic Tab Options · · · · · · · · · · · · · 32
2.8 Advanced Tab Options · · · · · · · · · · · 36
2.9 Plugins · · · · · · · · · · · · · · · · · 39
2.10 Start and End GCODE Settings · · · · · · · · 41
2.11 Expert Settings · · · · · · · · · · · · · 42
2.12 Retraction · · · · · · · · · · · · · · · 42
2.13 Skirt · · · · · · · · · · · · · · · · · · 43
2.14 Cool · · · · · · · · · · · · · · · · · · 44
2.15 Support · · · · · · · · · · · · · · · · · 45
iii
PROOF
Page 6
CONTENTS
2.16 Black Magic · · · · · · · · · · · · · · · 46
2.17 Brim · · · · · · · · · · · · · · · · · · 46
2.18 Raft · · · · · · · · · · · · · · · · · · 46
2.19 Fix Horrible · · · · · · · · · · · · · · · 48
2.20 Dual Extrusion · · · · · · · · · · · · · · 49
3 Printing with the Graphic LCD · · · · · 55
3.1 Graphical LCD Controller, Cura or Other Host? · 56
3.2 Multiple Connections · · · · · · · · · · · 56
3.3 Putting Print Files on the SD Card · · · · · · 57
3.4 Printing With the Graphical LCD Controller · · 57
3.5 Configuration Options · · · · · · · · · · · 60
3.6 Advanced Settings · · · · · · · · · · · · · 61
4 Maintaining Your 3D Printer · · · · · · 65
4.1 Overview · · · · · · · · · · · · · · · · 66
4.2 Smooth Rods · · · · · · · · · · · · · · · 66
4.3 Lead Screw Drive Rods · · · · · · · · · · · 66
4.4 PEI Print Surface · · · · · · · · · · · · · 66
4.5 Hobbed Bolt · · · · · · · · · · · · · · · 67
4.6 Belts · · · · · · · · · · · · · · · · · · 67
4.7 Hot End · · · · · · · · · · · · · · · · · 67
4.8 Nozzle Wiping Pad · · · · · · · · · · · · · 67
4.9 Bed Leveling Washers · · · · · · · · · · · 68
4.10 Cooling Fans · · · · · · · · · · · · · · · 68
4.11 Electronics · · · · · · · · · · · · · · · 68
5 Advanced Usage · · · · · · · · 69
5.1 Intro · · · · · · · · · · · · · · · · · · 70
5.2 Changing nozzles · · · · · · · · · · · · · 70
5.3 Bed Adhesion · · · · · · · · · · · · · · · 70
5.4 Using 1.75mm filament · · · · · · · · · · · 71
6 Hardware and Software Source Code · · · · 73
7 3D Printer Support · · · · · · · 75
7.1 LulzBot · · · · · · · · · · · · · · · · · 76
7.2 Support · · · · · · · · · · · · · · · · · 76
7.3 Regional Phone Numbers · · · · · · · · · · · 76
7.4 Community · · · · · · · · · · · · · · · · 76
iv
PROOF
Page 7
CONTENTS
8 Warranty Information · · · · · · · 77
8.1 Warranty · · · · · · · · · · · · · · · · 78
8.2 Modification Warning · · · · · · · · · · · 78
9 Contact Information · · · · · · · 79
9.1 Support · · · · · · · · · · · · · · · · · 80
9.2 Sales · · · · · · · · · · · · · · · · · · 80
9.3 Regional Phone Numbers · · · · · · · · · · · 80
9.4 Websites · · · · · · · · · · · · · · · · 80
Index · · · · · · · · · · · 81
Glossary · · · · · · · · · · 85
v
PROOF
Page 8
List of Figures
2.1 Quick Print Settings · · · · · · · · · · · · · · 19
2.2 Options after selecting model · · · · · · · · · · · 21
2.3 Rotating your Model · · · · · · · · · · · · · · 22
2.4 Scaling your Model · · · · · · · · · · · · · · 23
2.5 View in Normal Mode · · · · · · · · · · · · · 24
2.6 View in Overhang · · · · · · · · · · · · · · · 24
2.7 View in Ghost · · · · · · · · · · · · · · · · 25
2.8 View in Xray · · · · · · · · · · · · · · · · 25
2.9 View in Layers · · · · · · · · · · · · · · · · 26
2.10 Viewing Cumulative Layers · · · · · · · · · · · 26
2.11 Viewing Specic Layers · · · · · · · · · · · · · 27
2.12 Control Screen · · · · · · · · · · · · · · · · 29
2.13 View in Full Settings · · · · · · · · · · · · · · 31
2.14 Dierences in Layer Height · · · · · · · · · · · 32
2.15 Support Types · · · · · · · · · · · · · · · · 35
2.16 Cuto Example · · · · · · · · · · · · · · · 38
2.17 View of Plugins · · · · · · · · · · · · · · · 40
2.18 View Expert Settings · · · · · · · · · · · · · 42
2.19 Before Merge · · · · · · · · · · · · · · · · 52
2.20 After Merge · · · · · · · · · · · · · · · · · 52
3.1 GLCD Info Screen · · · · · · · · · · · · · · 57
3.2 Main Menu · · · · · · · · · · · · · · · · · 59
3.3 Z Oset Screen · · · · · · · · · · · · · · · · 62
3.4 GLCD Map · · · · · · · · · · · · · · · · · 64
vi
PROOF
Page 9
WARNINGS
Safety Information
PROOF
Page 10
WARNING!
Read Me First!
READ THIS MANUAL COMPLETELY BEFORE UNPACKING AND
POWERING UP YOUR PRINTER.
Hazards and Warnings
Your LulzBot®TAZ 3D printer has motorized and heated parts. Always
be aware of possible hazards when the printer is operational.
Electric Shock Hazard
Never open the electronics case when the printer is powered on. Before
removing the electronics case cover, always power down the printer and
completely turn o and unplug the printer. Allow the printer to discharge
for at least one minute.
Burn Hazard
Never touch the hot end nozzle or heater block without rst turning o the
hot end and allowing it to completely cool down. The hot end can take up
to 20 minutes to completely cool. Never touch recently extruded plastic.
The plastic can stick to your skin and cause burns. The print surface can
reach high temperatures that are capable of causing burns.
Fire Hazard
Never place ammable materials or liquids on or near the printer when it
is powered on or operational. Liquid acetone, alcohol, or other chemicals
may release vapors that are extremely ammable.
Pinch Hazard
When the printer is operational take care to never put your ngers near
any moving parts including belts, pulleys, or gears. Tie back long hair or
clothing that can get caught in the moving parts of the printer.
viii
PROOF
Page 11
REGULATORY COMPLIANCE STATEMENT CLASS B
Age Warning
For users under the age of 18, adult supervision is recommended. Beware
of choking hazards around small children.
Modications and Repairs Warning
At Aleph Objects, Inc. we respect your freedom to modify your LulzBot
®
desktop 3D printer. However any modications or attempted repairs that
cause damage are not covered under the Warranty. Questions? Contact
Technical Support by emailing [email protected], or by calling +1970-377-1111.
Regulatory Compliance Statement Class B
Federal Communications Commission Statement
CAUTION: Changes or modications not approved by the party responsible for compliance could void the users authority to operate the equipment.
NOTE: This equipment has been tested and found to comply with the
limits for a Class B digital device, pursuant to part 15 of the FCC Rules.
These limits are designed to provide reasonable protection against harmful
interference in a residential installation. This equipment generates, uses
and can radiate radio frequency energy and, if not installed and used in
accordance with the instructions, may cause harmful interference to radio
communications. However, there is no guarantee that interference will not
occur in a particular installation. If this equipment does cause harmful
interference to radio or television reception, which can be determined by
turning the equipment o and on, the user is encouraged to try to correct
the interference by one or more of the following measures:
1. Reorient or relocate the receiving antenna.
2. Increase the separation between the equipment and receiver.
3. Connect the equipment into an outlet on a circuit dierent from that
to which the receiver is connected.
4. Consult the dealer or an experienced radio/TV technician for help.
ix
PROOF
Page 12
WARNING!
Industry Canada Statement
Cet appareil numérique de la classe B est conforme à la norme ICES-003
du Canada. This device complies with Canadian ICES-003 Class B.
Australian Communications and Media Authority
Statement
This device has been tested and found to comply with the limits for a
Class B digital device, pursuant to the Australian/New Zealand standard
AS/NZS CISPR 22:2009 + A1:2010.
x
PROOF
Page 13
3D Printer Software
PROOF
Page 14
3D Printer Software
1.1 Software Overview
To operate your desktop 3D printer you will need to install a few software
packages onto your PC. You will need a 3D printer host, an .STL to .GCODE
generator, and optional CAD or 3D modeling software.
Cura LulzBot®Edition is the recommended software for your
LulzBot 3D printer. Download Cura LulzBot Edition by visiting
LulzBot.com/Cura.
All of the following Free/Libre Software packages are available for
GNU/Linux, Windows, and OS X. We highly recommend using these
programs on GNU/Linux.
1.2 Software Types
Printer Hosts
Printer Host software is used to control the 3D printer. The program
not only allows you to manually move the printer along all the axes,
but set temperatures manually, send commands, and receive feedback/error messages from the onboard electronics. We recommend
that new users start with Cura LulzBot®Edition as it includes a
slicing engine as well.
Slicers
These programs take the 3-Dimensional model (typically
STL/OBJ/etc) and determine the 3D printer toolpath based
on the options selected. The slicing engine uses the nozzle diameter,
movement speeds, layer height, and other variables to determine the
coordinates where it needs to move, and the rates at which it will do
so. This information is exported out of the program as a GCODE
le. The GCODE le is a plain-text le with a series of text-based
codes and a list of the complete X,Y, and Z-axis coordinates used
for printing the 3D model. We recommend that new users start with
Cura LulzBot Edition as it includes the printer host as well.
12
PROOF
Page 15
1.3. INSTALLING DRIVERS
1.3 Installing Drivers
GNU/Linux and OS X users will not need to install a driver to communicate
with the LulzBot TAZ 3D printer. Windows users will need to install
the drivers. Using Cura LulzBot Edition as your printer host and slicing
software is recommended, as the drivers will automatically be installed
during the Cura installation process. Download Cura LulzBot Edition
by visiting LulzBot.com/Cura. The drivers can also be downloaded from
LulzBot.com/downloads. A visual guide showing the driver installation
process can be found in our download section as well.
1.4 CAD and 3D Modeling Software
LulzBot is not distributing a CAD or 3D modeling software package.
However, multiple Free/Libre Software packages are available. Other
common non-free CAD and 3D modeling software are also capable of
exporting the required .STL les.
On some CAD and 3D modeling software you will need to select
millimeters as the output unit. If possible it is best to build your 3D
design in metric units rather than imperial units. Cura requires .STL les
sized in millimeters. If an .STL with inches as units is loaded into Cura, the
model will be scaled much smaller than expected. You can scale the model
by 25.40 to compensate. The software listed below outputs millimeters as
the unit by default.
FreeCAD
Website: http://www.freecadweb.org/
Although still in development, contains a full GUI for building CAD
models. FreeCAD is capable of creating simple to complex designs. STL
les can also easily be exported for use with 3D printing. FreeCAD is
available for GNU/Linux, Windows, and OS X. The latest development
version is recommended.
OpenSCAD
Website: http://openscad.org
13
PROOF
Page 16
3D Printer Software
OpenSCAD is dierent than FreeCAD in that it is script based. Rather
than using a GUI to generate CAD designs, OpenSCAD CAD designs are
created using script based renderings. Users with programming experience
would nd this useful. Also, OpenSCAD uses a simple script language that
is easy for users with little or no programming experience to learn.
Blender
Website: http://blender.org
The most widely used Free/Libre Software 3D modeling software,
Blender is well documented with tutorials available on the Blender.org
website as well as found online.
Shapesmith
Website: http://shapesmith.net
Shapesmith is a web-based 3D modeling software. This means there is
no required software to get started designing models. Shapesmith is also a
great choice for anyone starting out in CAD/ 3D modeling.
1.5 Alternative Printer Host Software
OctoPrint
Website: http://octoprint.org/
Octoprint is a printer host that uses a web-based interface to access and
control your 3D printer. Added web-cam functionality allows for time-lapse
videos and a live stream. Octoprint will run on GNU/Linux, Windows, OS
X based computers and can even run well on a Beagle Bone Black or a
RaspberryPi (inexpensive business-card sized computers).
BotQueue
Website: https://www.botqueue.com/
BotQueue works well for those users wanting to have a web-based
multiple 3D printer operation running o a queuing system.
14
PROOF
Page 17
1.5. ALTERNATIVE PRINTER HOST SOFTWARE
MatterControl
Website: http://www.mattercontrol.com/
MatterControl is another printer host that currently runs on
GNU/Linux, Windows, and OS X. It features 2D and 3D model viewing,
a print queue, and print le organization and searching.
Source Files
Aleph Objects, Inc., the maker of the LulzBot®TAZ 3D printer, completely
supports Free Software, Libre Innovation, and Open Source Hardware.
Along with the LulzBot TAZ 3D printer being a Free Software and Open
Source Hardware design, it has been tested to work with 100% Free/Libre
Software. Our source code and design les are hosted on:
LulzBot Download Server http://download.lulzbot.com
LulzBot Development Server http://devel.lulzbot.com
Aleph Objects Code Repository http://code.alephobjects.com
Aleph Objects Download Server http://download.alephobjects.com
Aleph Objects Development Server http://devel.alephobjects.com
15
PROOF
Page 18
PROOF
Page 19
Cura LulzBot Edition
PROOF
Page 20
Cura LulzBot Edition
2.1 Cura
Setup Cura
Cura LulzBot Edition is available for download on our website at
http://LulzBot.com/cura. When installing, it is recommended to uninstall any previous versions of Cura you may have been using. Cura
is designed for Fused Filament Fabrication (FFF) 3D printers. Fused
Filament Fabrication is the term for the process of laying down successive
layers of extruded lament to create a 3 dimensional object. As each layer
of molten plastic is extruded into place, it fuses with the previous layer.
When rst opening Cura, you will be prompted to go through the First
run wizard. This will consist of selecting your printer, hot end type, tool
head type, and nally your nozzle diameter.
It is important to select the correct printer, hot end, tool head, and
nozzle diameter as Cura uses custom proles and machine settings based
upon which printer, hot end, tool head, and nozzle you have.
• Download the appropriate installer for your computer operating
system. Instructions on installation for each operating system are
available at http://LulzBot.com/cura.
• Install Cura by double clicking on the installer.
• Click through the install wizard until it completes.
• Start Cura by launching it from your list of installed applications.
If this is the rst time that Cura has been used the “Conguration
Wizard” window will open.
• Select LulzBot TAZ 6. Press Next.
• Select Single Extruder v2.1. Press Next
• Select nish.
18
PROOF
Page 21
2.2. QUICK PRINT SETTINGS
2.2 Quick Print Settings
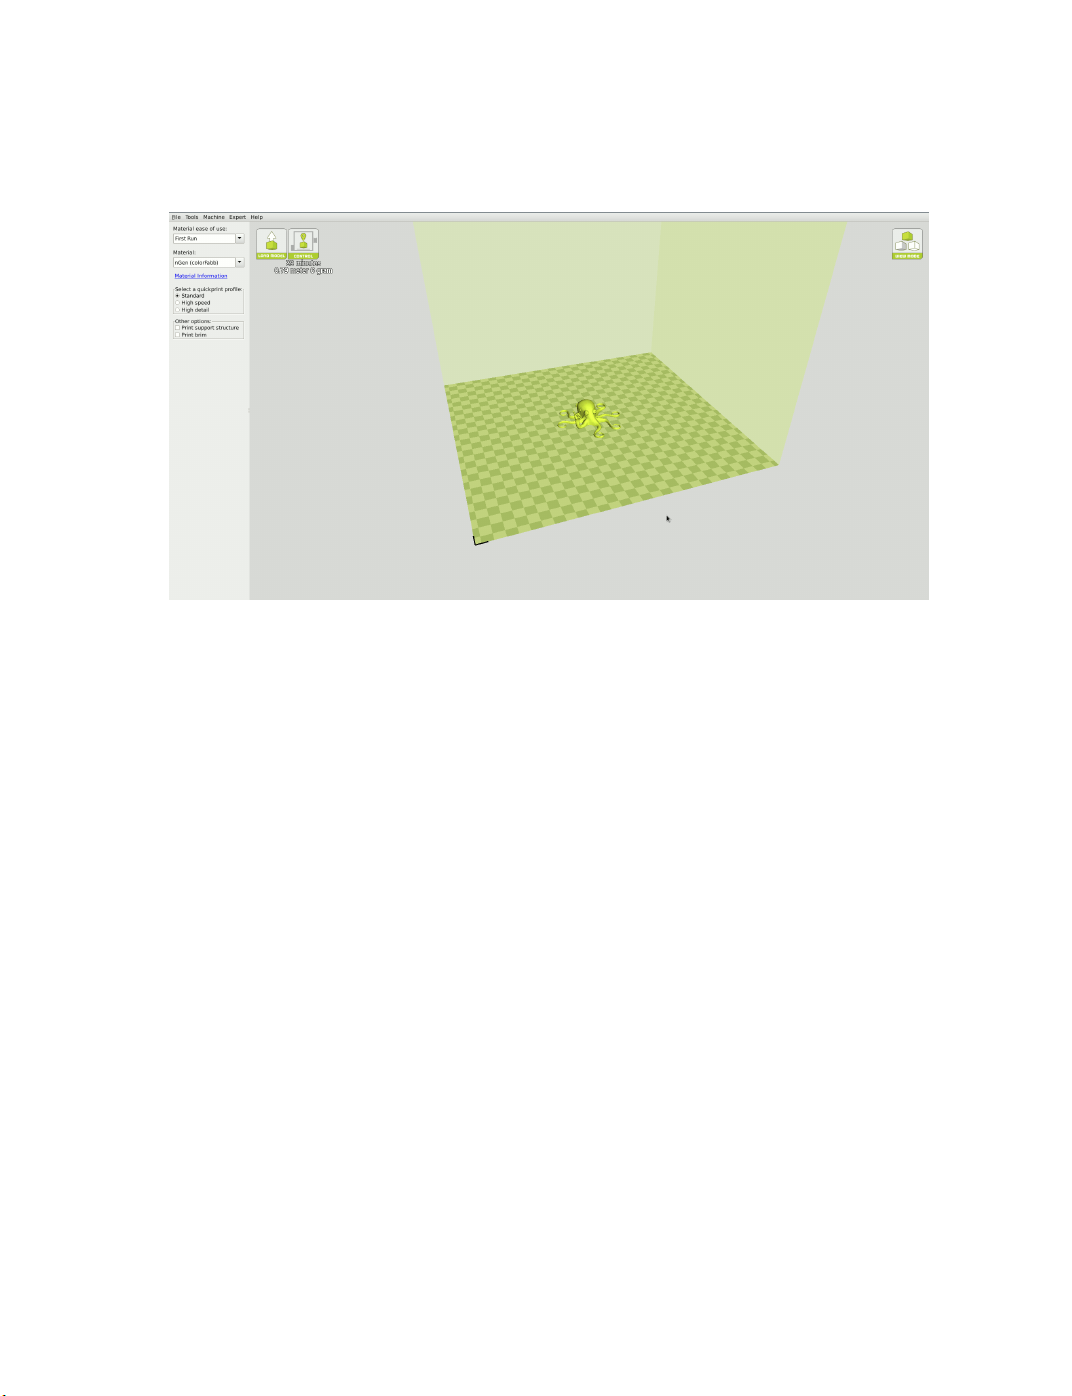
Figure 2.1: Quick Print Settings
After setting up Cura for the rst time, you will be shown the main interface
screen. (Fig. 2.1, page 19)
Selecting a Quick Print Profile
The print quality settings can be found in the top left-hand corner of the
window. For most laments, there will be Standard, High Speed, and
High Detail options. Some of the more exotic laments may only have a
single prole.
High Detail
Designed to give greater detail and ner objects. This will have a
smaller layer height, which will make each layer thinner, so that curves
seem more natural and walls seem less noticeable. This setting will
also require more layers to be laid down, increasing overall print time.
Standard
Designed to give a balanced resolution by increasing the layer height
19
PROOF
Page 22
Cura LulzBot Edition
and print speeds. This will make the organic curves slightly more
step-like than the ne setting, but it will reduce printing time.
High Speed
Designed for the fast prints, where the overall model nish is not of
concern. Most commonly used for quick iteration of designs when
rapid prototyping.
Material Selection
We have the dierent laments separated by Material ease of use. From
the Material ease of use drop down, select "All" to view all our preloaded lament slicing proles. The TAZ ships with a lament sample for
the rst print. Refer to the included Quick Start Guide for the proper
“First Run” settings.
Printing Support Material
The LulzBot TAZ 3D printer is able to print models that have angles
and overhangs, even without support material. This will depend on the
overhang distance and angle of your particular model le. Turn this option
on if your model could benet from support material.
Brim
Brim is used to increase surface area of the part you’re printing, thereby
ensuring proper part adhesion. This will print a single layer high edge
around the base of the part, helping rst layer adhesion and minimizing
warping.
Load Model File
Select the STL model you would like to print. Either use the Load Model
button or select File > Load Model. Once the le has been loaded, you
will see a 3D rendering of your object on the build platform. Select the
model to see the various options.
20
PROOF
Page 23
2.2. QUICK PRINT SETTINGS
Model Orientation
Move your model to change where it is printed on the build plate. Do this
by left clicking on the model and dragging it to the desired location. The
black outlined corner of the 3D print bed view represents the front left
hand corner of the build plate on your printer. By holding down the right
mouse button and dragging, you can view your model from dierent angles.
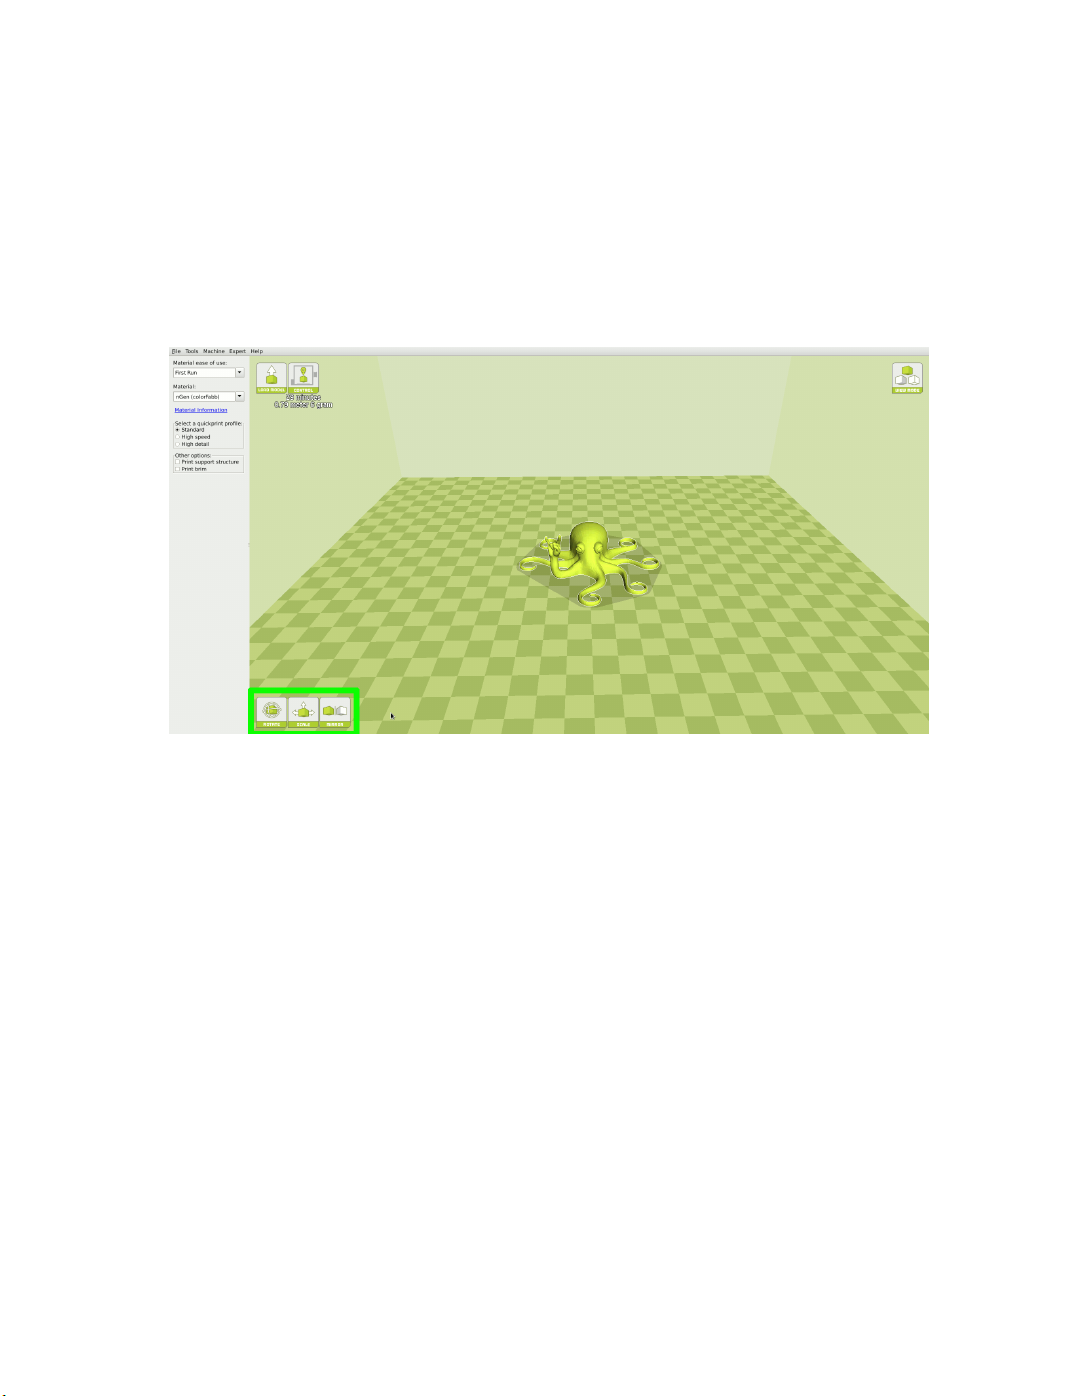
Figure 2.2: Options after selecting model
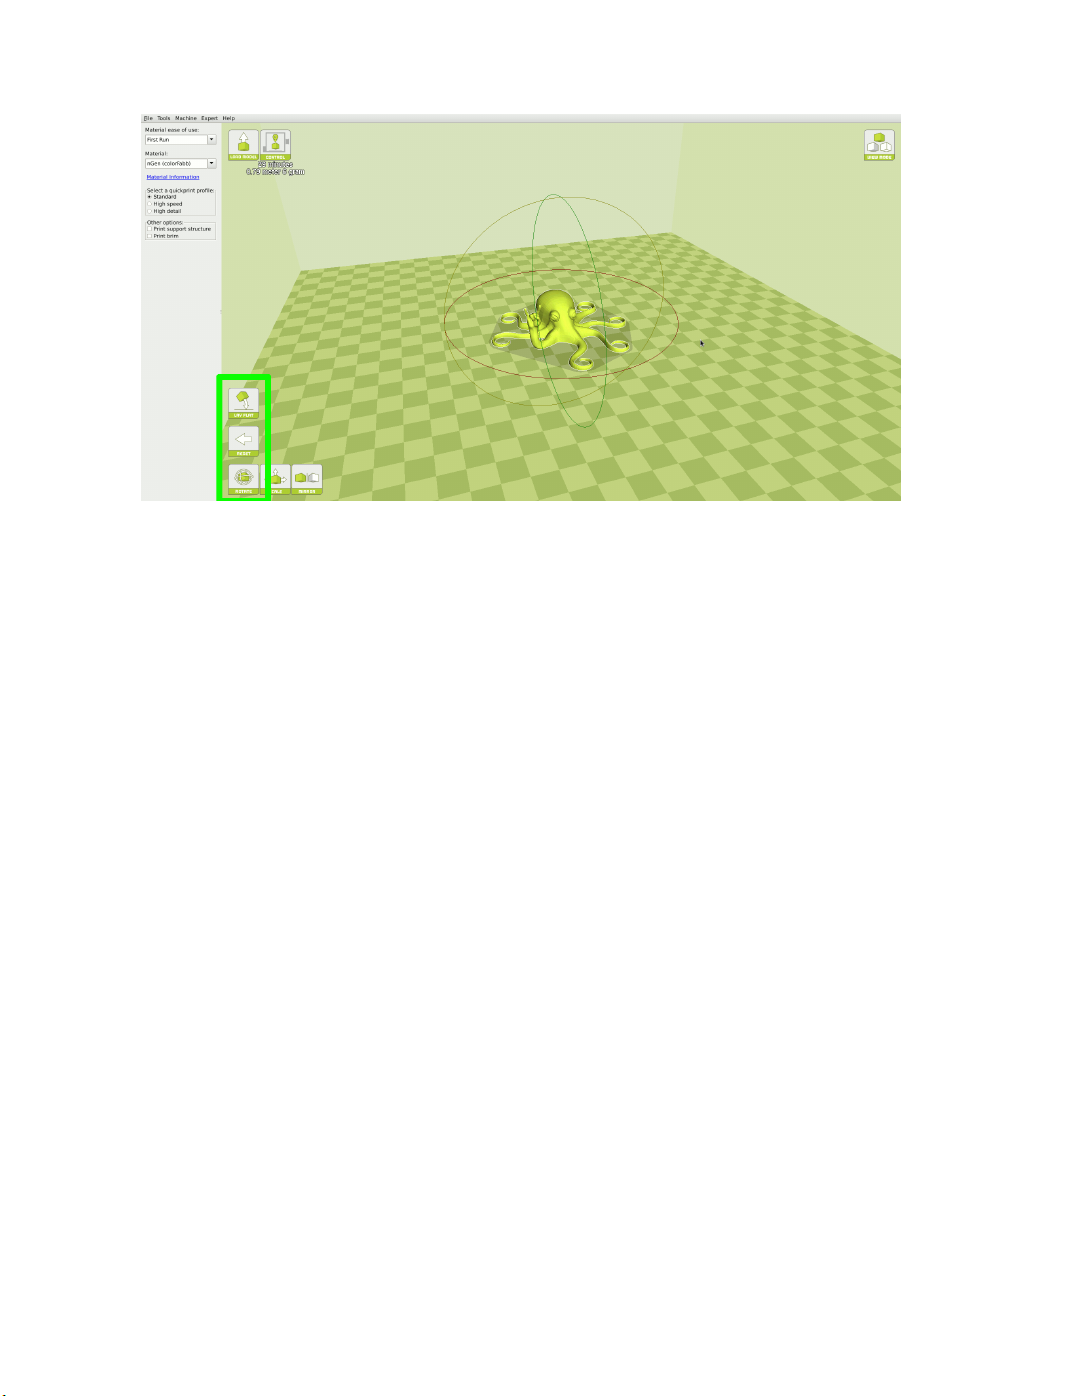
Rotate
The Rotate button will give you the ability to orient your model in along
all three axes. Once you click the rotate button, three circles will surround
your model. The red circle will allow you to rotate around the Z-axis. The
Yellow circle will rotate around the Y-axis. The Green circle will rotate
around the X-axis. Cura defaults to 15 degree increments. Hold Shift to
rotate by One Degree Increments.
21
PROOF
Page 24
Cura LulzBot Edition
Figure 2.3: Rotating your Model
Lay Flat
The Lay Flat button will ensure that the at portion of your print is
securely attached to the bed. It is highly recommended to use this option
after rotating your model in the Z direction, as it will help prevent potential
adhesion issues during the print.
Reset
The Reset button will return your model to the original orientation as
dened by the CAD program used to create the model.
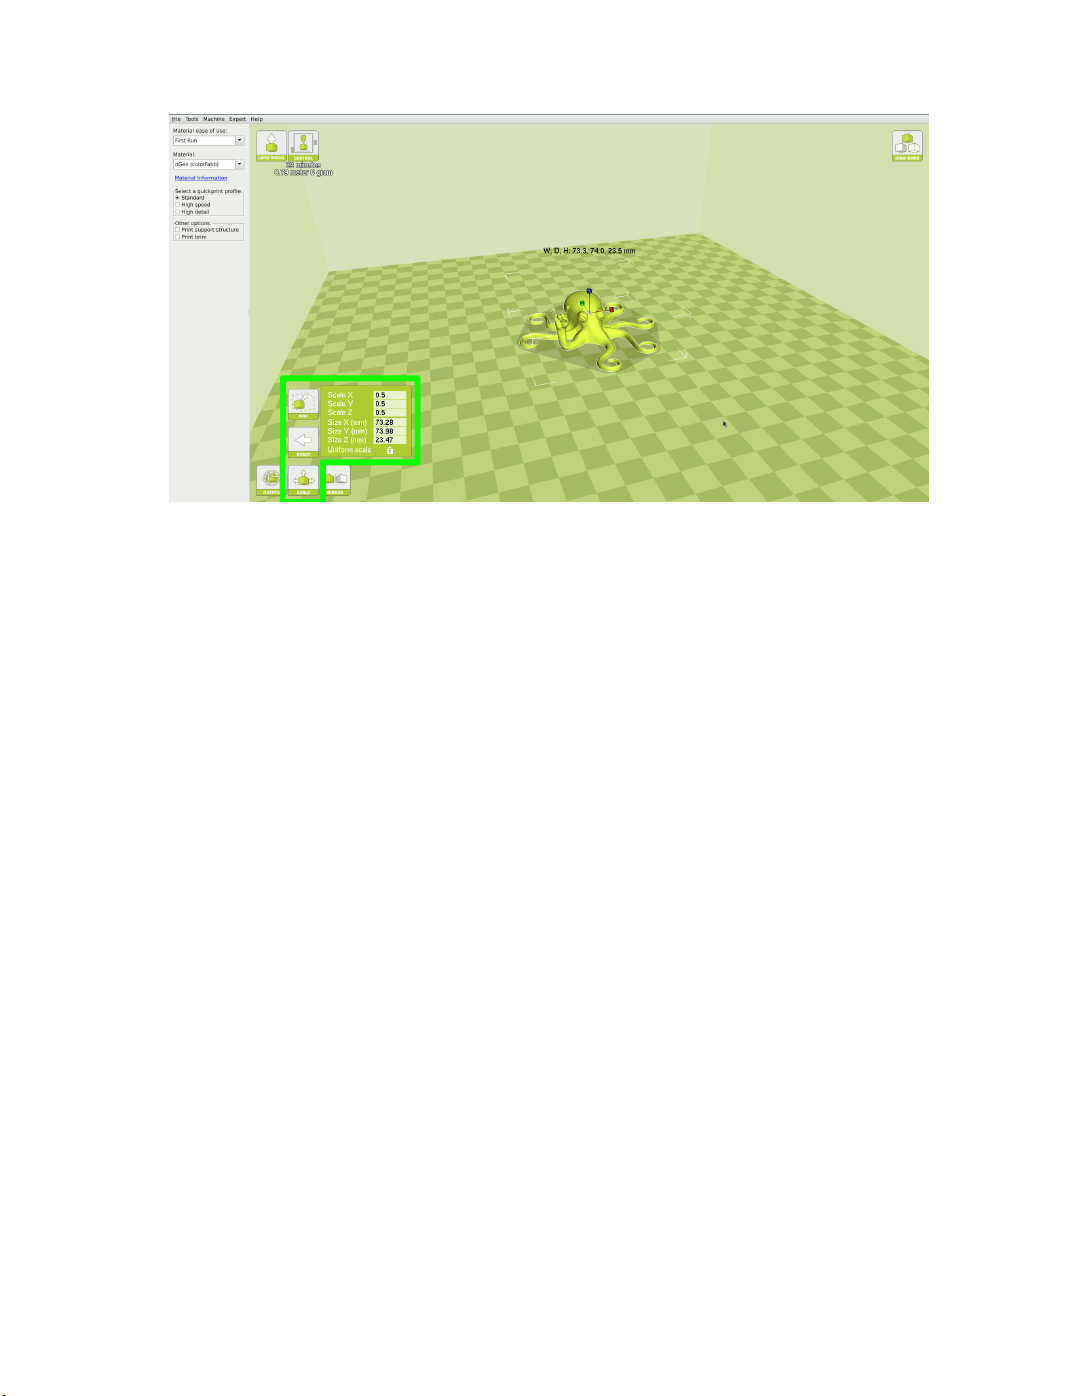
Scale
The Scale button displays the model dimensions, along with the ability to
scale along the X Y or Z axes. Anything below the number 1.0 will reduce
the objects size, while anything above the number 1.0 will increase the
objects size. As a default, it will be set to uniform scaling. This will cause
the X Y and Z axes to be scaled by the same amount when you make a
change to any of them. To disable this, select the lock in the lower section
of the scaling window.
22
PROOF
Page 25
2.3. VIEW OPTIONS
Figure 2.4: Scaling your Model
2.3 View Options
Dierent modes allow you to view your model in a variety of ways. This
can be helpful for spotting issues before the print even starts.
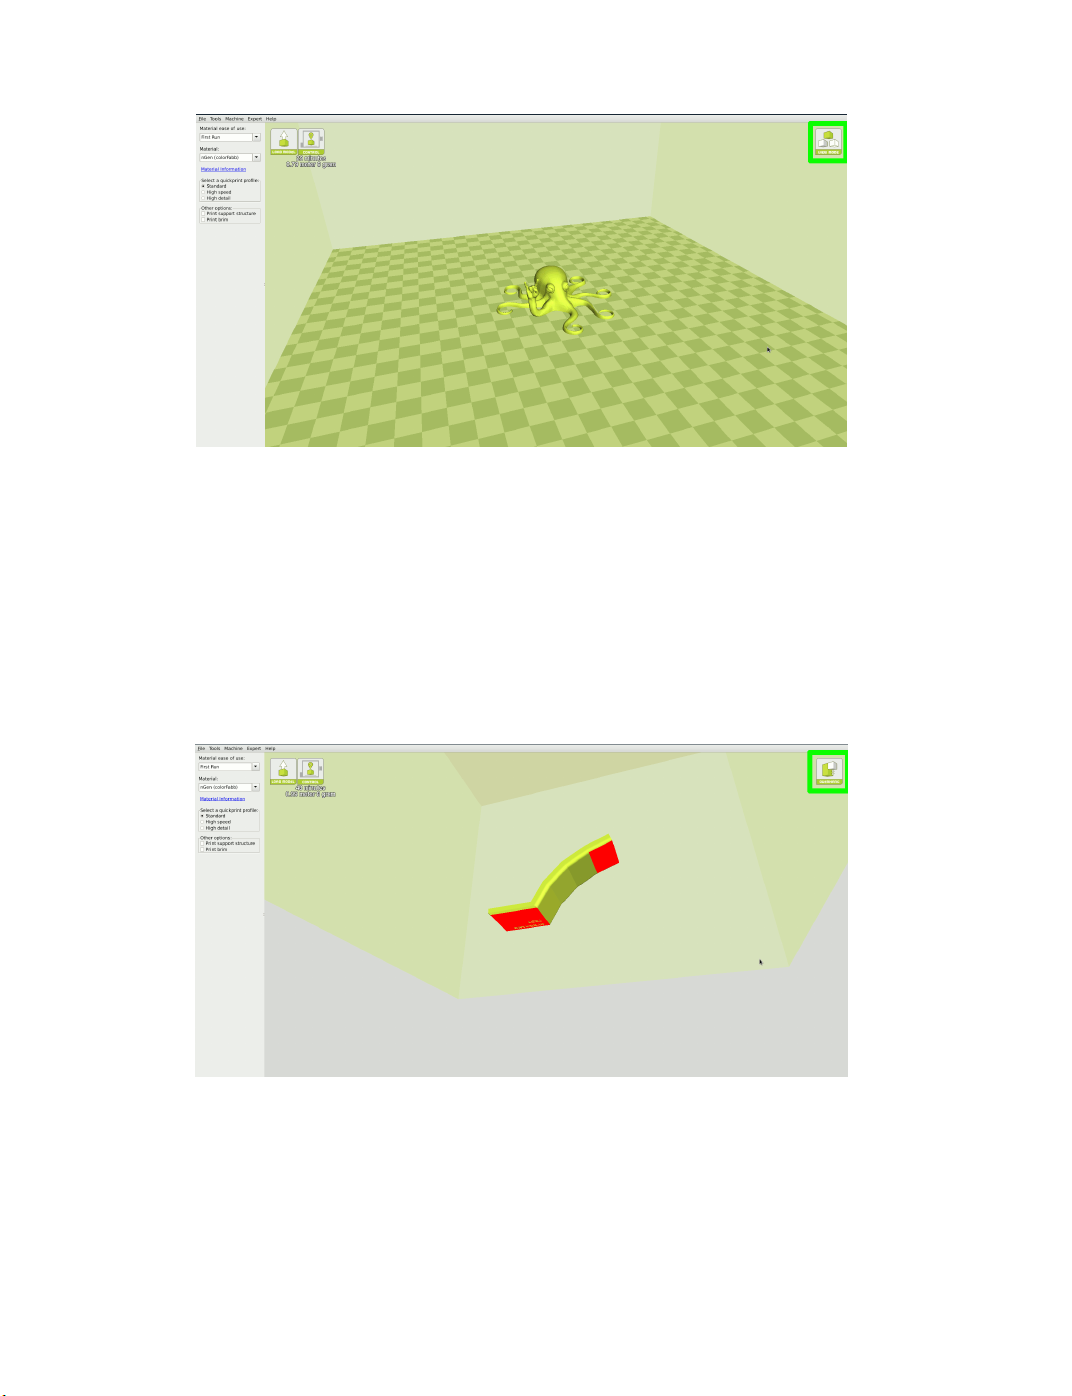
Normal
This is the standard view and shows the solid outer surfaces of the model.
(Fig. 2.5, page 24):
23
PROOF
Page 26
Cura LulzBot Edition
Figure 2.5: View in Normal Mode
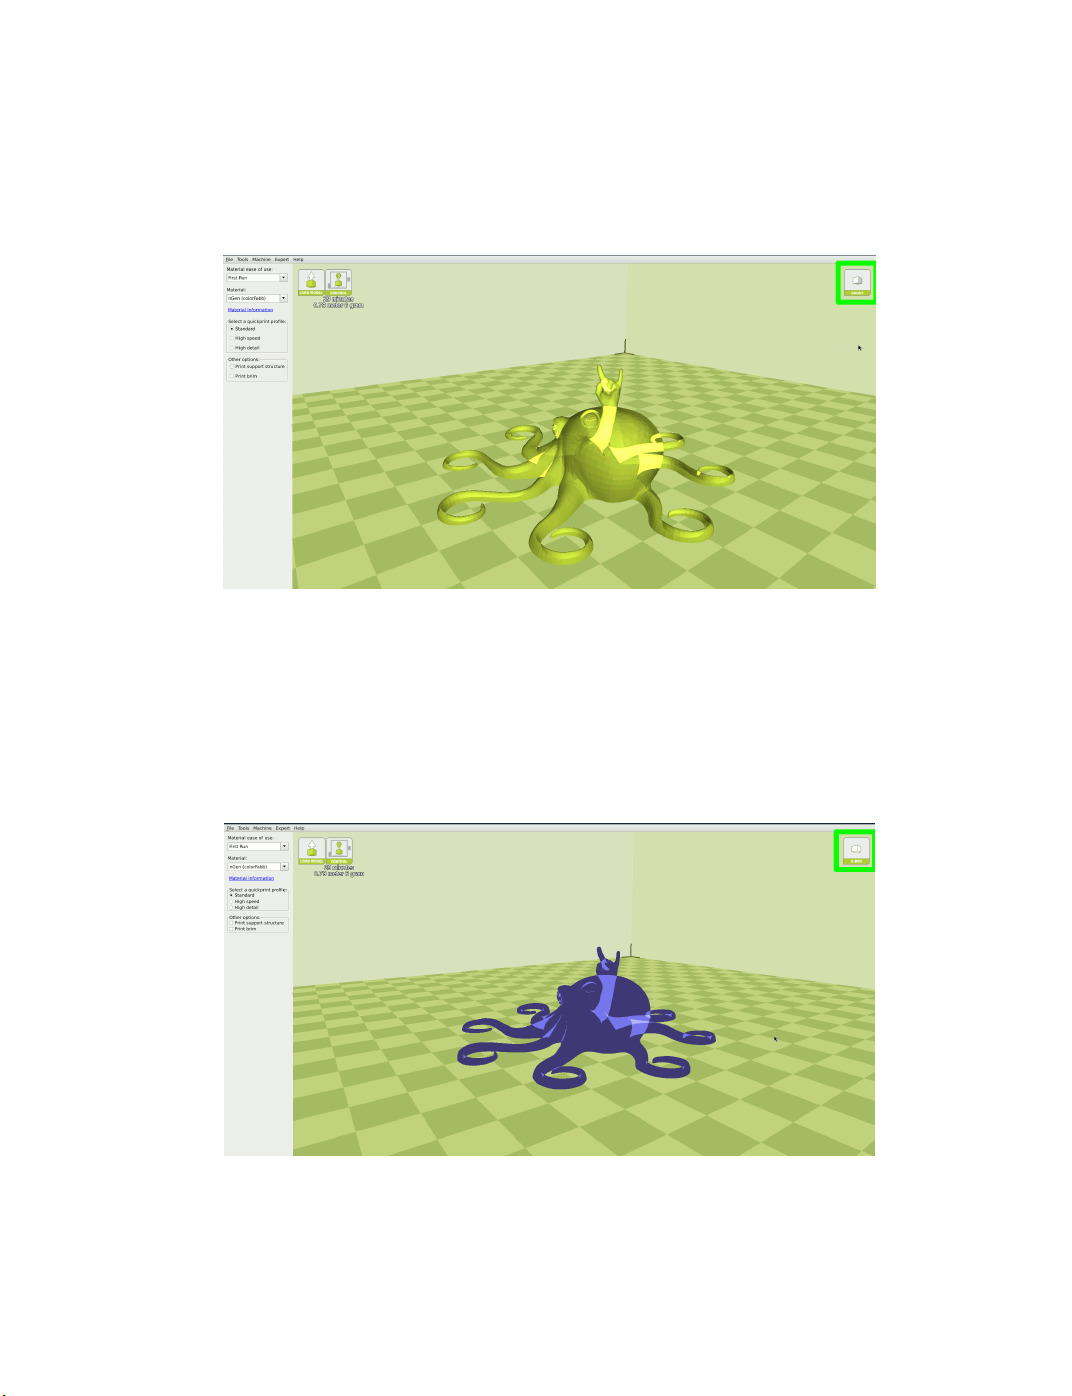
Overhang
Overhang mode shows where your model may need support material. In
Fig. 2.6, page 24 the red highlighted areas show overhangs and more severe
angles and areas where support material is recommended. The overhang
threshold can be dened in Expert Settings.
Figure 2.6: View in Overhang
24
PROOF
Page 27
2.3. VIEW OPTIONS
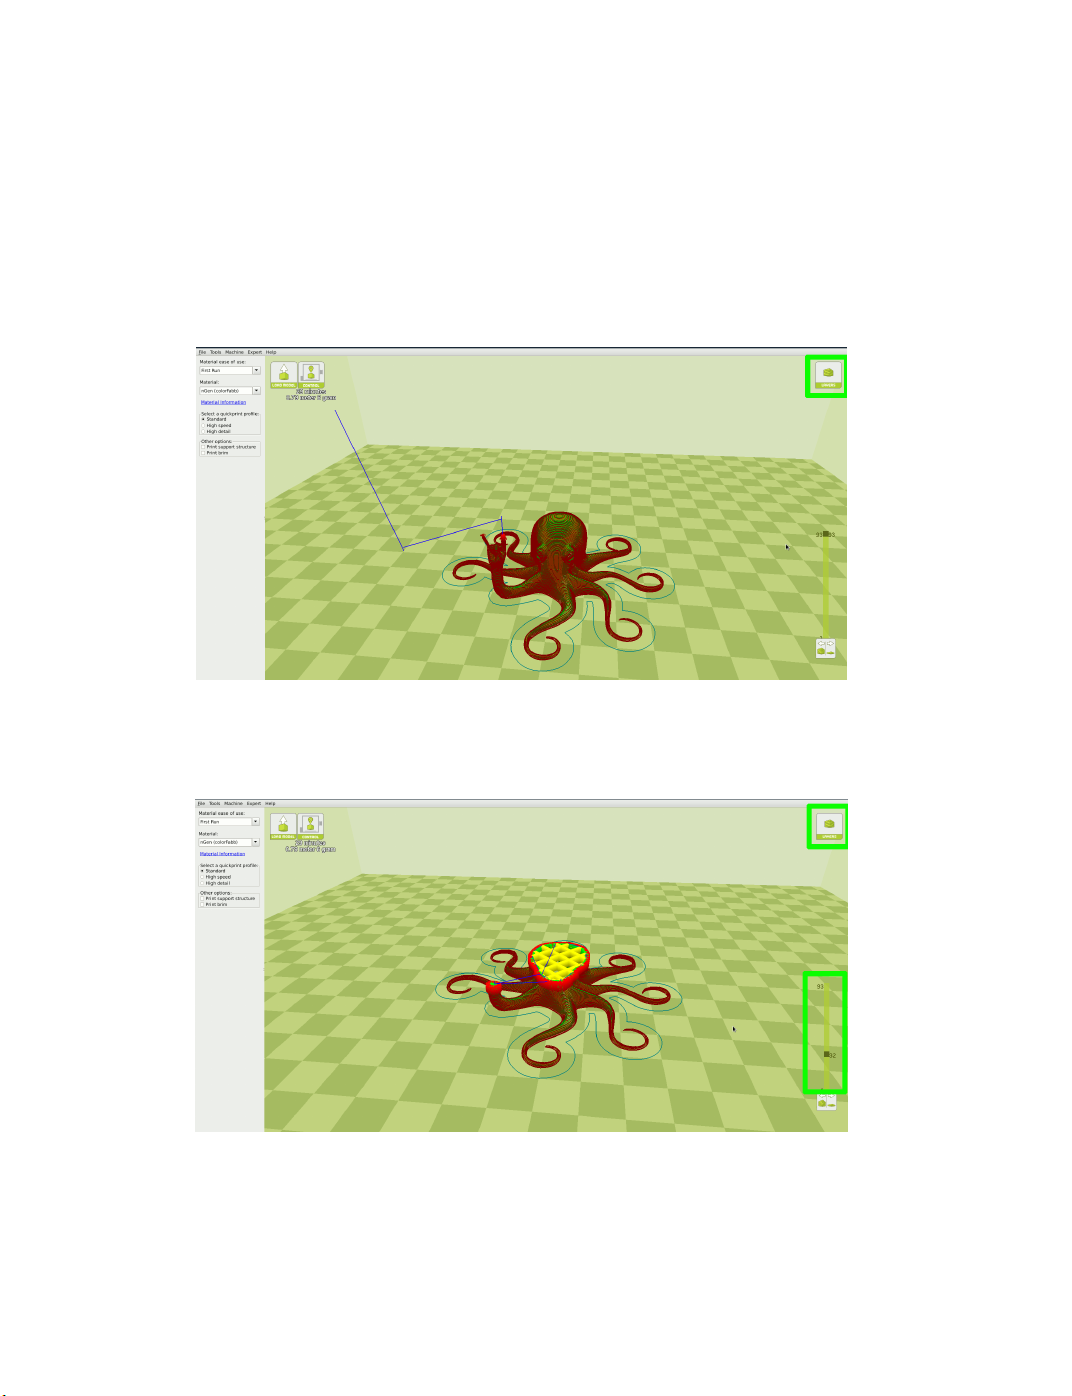
Ghost
Ghost view mode makes the model translucent to allow you to see what is
behind it.
Figure 2.7: View in Ghost
Xray
Xray is similar to Ghost mode. It will allow you to see into objects, ensuring
that inner details are correct.
Figure 2.8: View in Xray
25
PROOF
Page 28
Cura LulzBot Edition
Layers
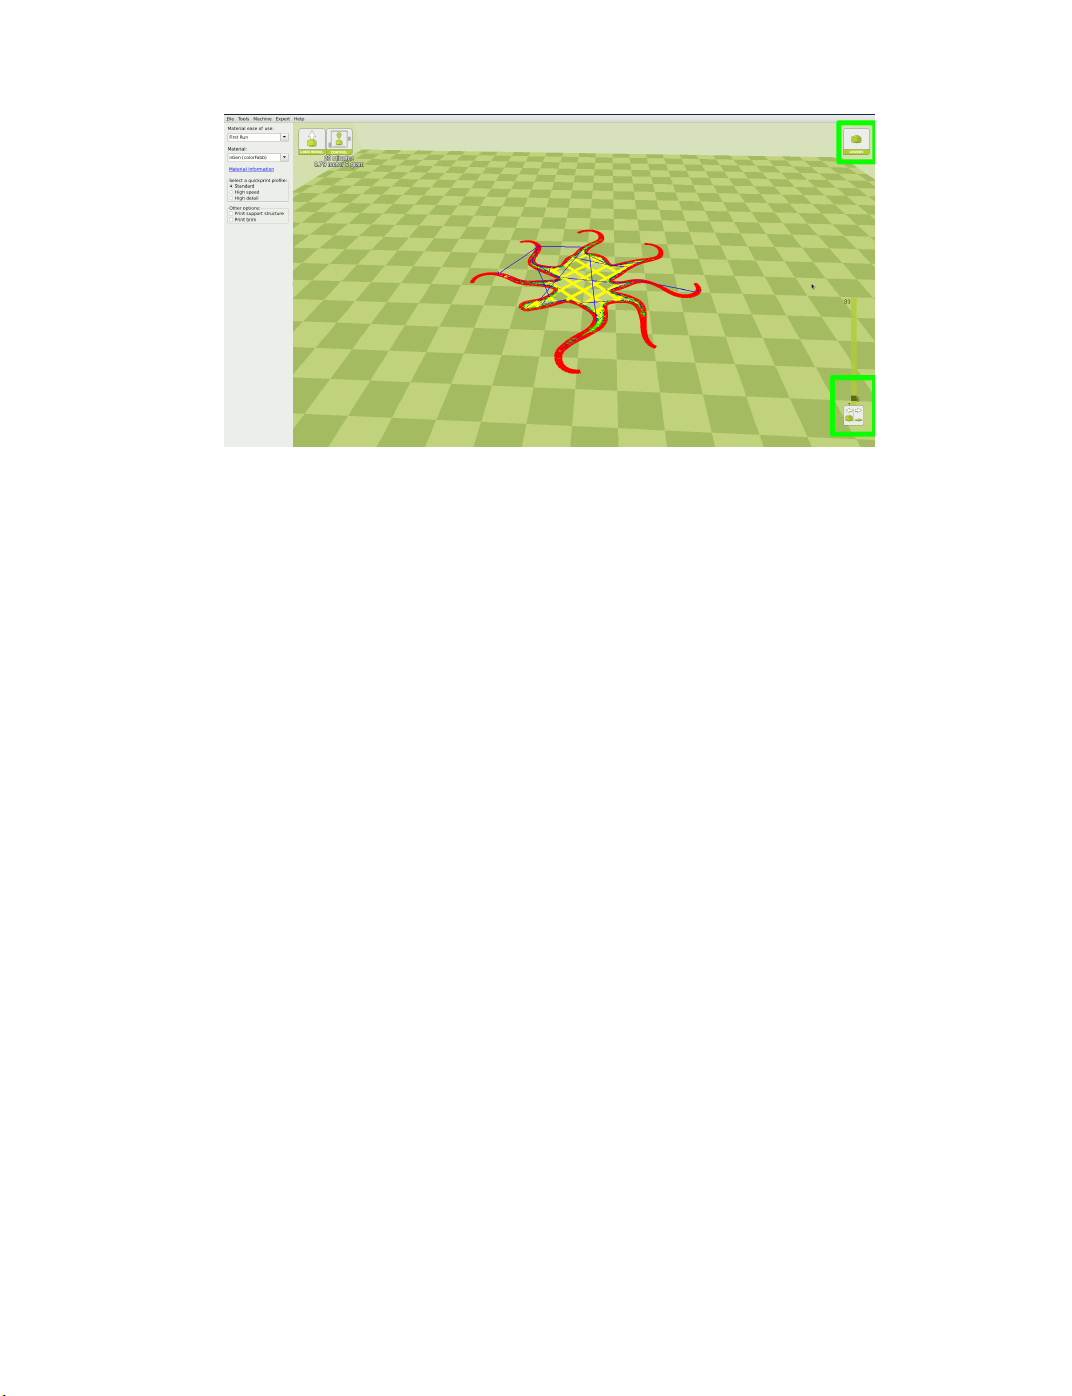
To view the tool path of your print head and to ensure no skipped layers or
gaps use this option. Use the slide bar on the right hand side of the window
to move up and down through the tool path layers. Click the icon below
it to view an individual layer at a time. If the Print support structure
option is activated in Cura, it will be shown in blue.
Figure 2.9: View in Layers
Figure 2.10: Viewing Cumulative Layers
26
PROOF
Page 29
2.4. STARTING YOUR FIRST PRINT
Figure 2.11: Viewing Specic Layers
2.4 Starting Your First Print
Once you have your model, prole, and lament loaded, it is time for your
rst print! Refer to the Quick Start Guide included with your 3D printer.
A PDF version is available at LulzBot.com/downloads.
Automatic Bed Leveling
Before each print your, TAZ will go through a wiping and a probing
procedure in order to determine the slope/tilt of your bed. If your nozzle is
dirty or not cleaned properly, this will prevent the printer from being able to
create an electrical contact with the corners. Your TAZ will automatically
retry the wiping and probing procedure if this happens, up to a maximum
of three times. If three consecutive wipes and probes have failed, the printer
will stop and a warning will sound. If this is happening consistently, you
should replace the wiping pad and/or adjust your wiping and probing temps
for that specic lament. See section 2.10 on page 41 for details on changing
these temps.
Printing from SD Card
Load your model into Cura with the proper lament and prole selected.
Next, insert the included SD card into your computer. Select File > Save
27
PROOF
Page 30
Cura LulzBot Edition
GCODE and choose the SD card location to save your GCODE le to your
SD card. Safely eject the card from the computer, and insert it into the
Graphical LCD Controller.
Start Print
Thanks to the TAZ automatic bed leveling system, it is now time to kick o
the print! Through the LCD screen go to: Print From SD > Desired File.
Your TAZ will then go through it’s automatic cleaning and wiping process
before starting the print. This should take approximately 5 minutes.
Printing from USB Cable
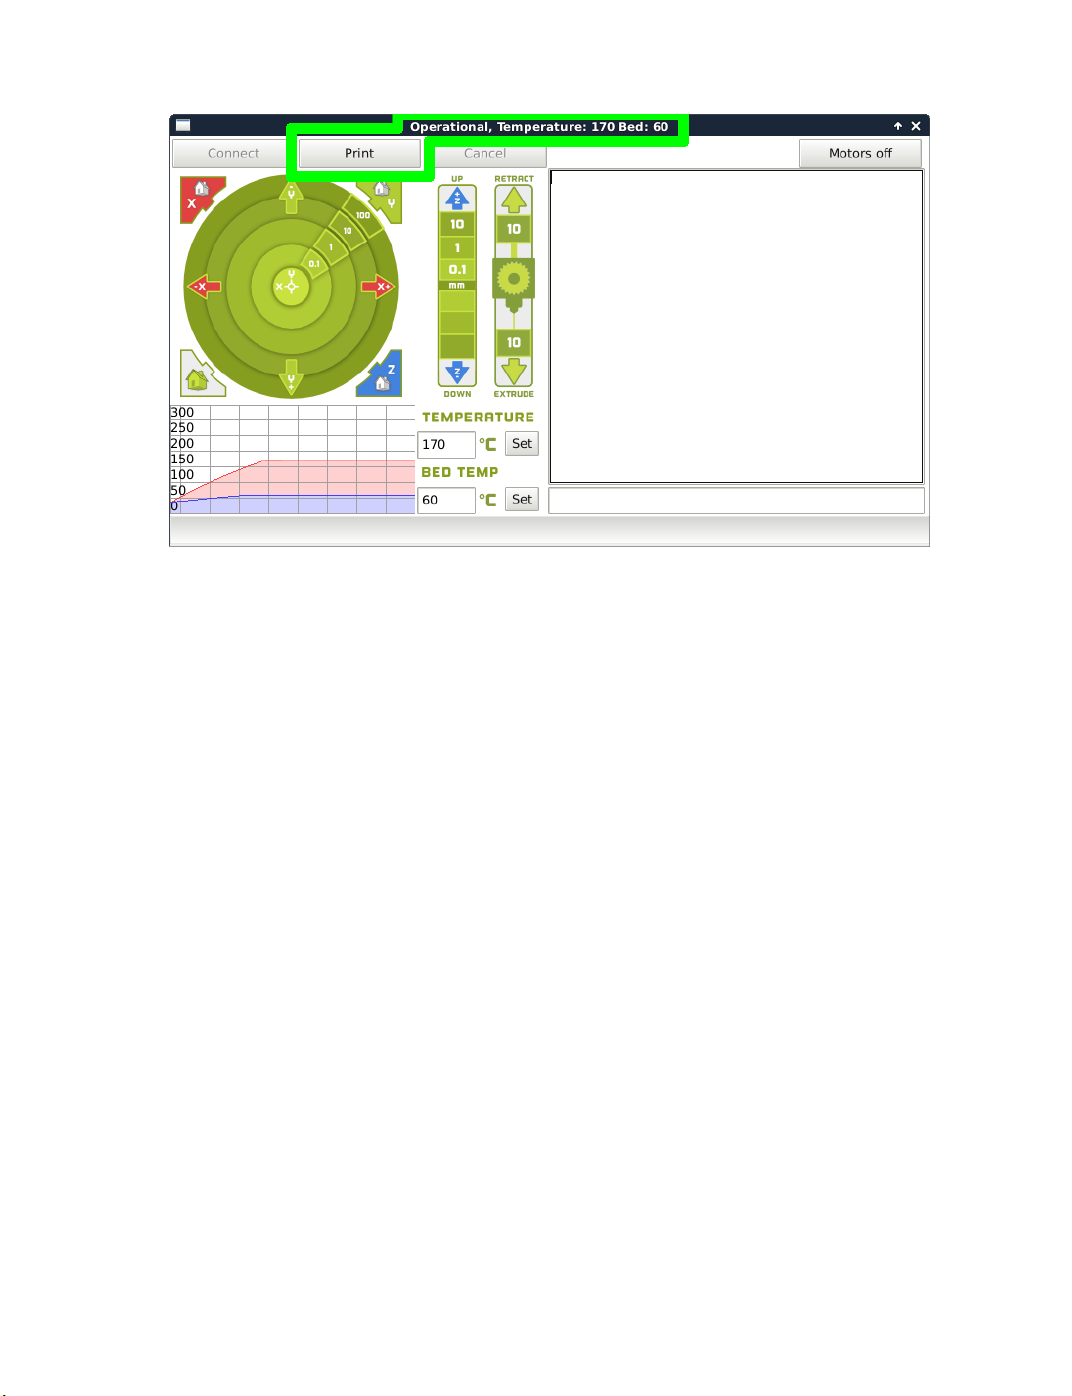
Connect your 3D printer to a computer using a USB cable, power it on
and select the Control button at the top of the 3D viewing window. If the
control button is not present, be sure you have a model le loaded into Cura.
If a model is loaded but the Control button is still not present use a dierent
USB cable, reinstall Cura, or contact our Support Team. This will bring
up your Printer Interface. You will not be able to send any commands until
the window title changes to Operational. Once operational, you can start
your rst print. Your TAZ will then go through it’s automatic cleaning and
wiping process before starting the print. This should take approximately 5
minutes.
28
PROOF
Page 31
2.4. STARTING YOUR FIRST PRINT
Figure 2.12: Control Screen
Pausing Mid-Print
You will notice after you click the print button through Cura, it will
change to a pause button. When activated, it will pause the print and
automatically move your print head away from your object. This will allow
color changes or material changes mid print.
Recommended Temperatures and Bed Preperation
When generating GCODE, it may be benecial to adjust temperatures
depending on your specic model le or lament. We have also found that
for certain materials applying unscented glue stick to the print surface is
required for successful bed adhesion and/or part release. Glue stick can also
be added to help rst layer adhesion on any material, and may be helpful
for objects with a larger surface area. You can nd our recommended
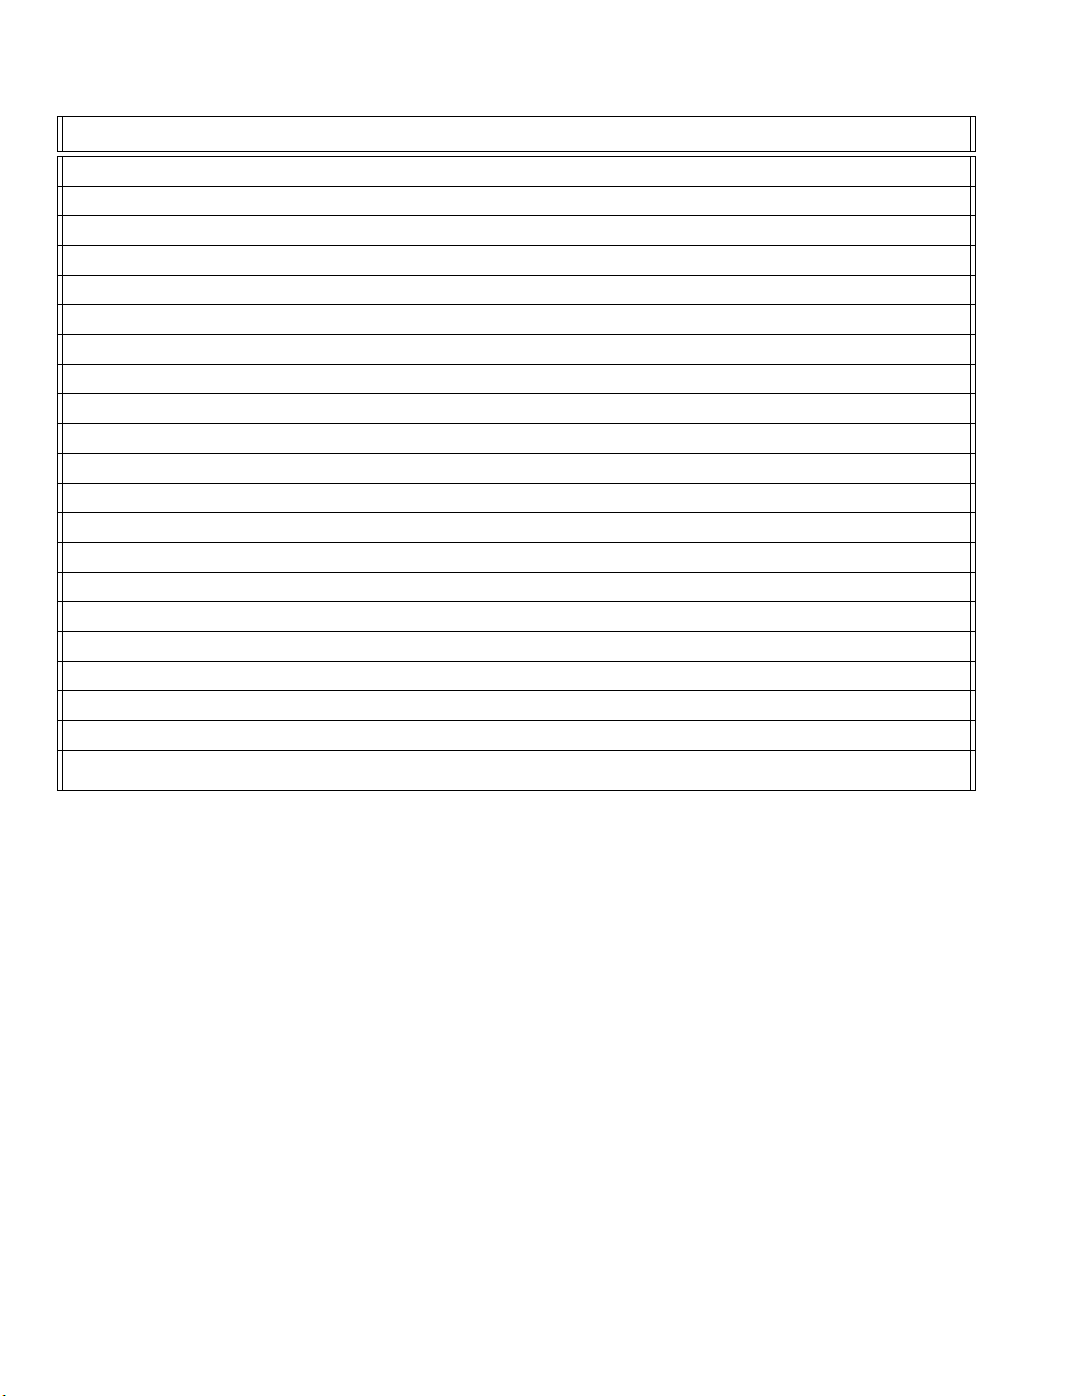
temperature ranges and adhesion techniques below.
29
PROOF
Page 32
Cura LulzBot Edition
Filament Type Bed Preparation Nozzle Temp Bed Temp Removal Temp
ABS Clean PEI 230-250 110 50
PLA Clean PEI 195-215 60 45
HIPS Clean PEI 230-250 110 50
Laywoo-D3 Clean PEI 175-195 60 45
bambooFill Clean PEI 185-195 60 50
woodFill Clean PEI 185-195 60 50
Laybrick Clean PEI 175-195 60 45
bronzeFill Clean PEI 225-235 60 50
copperFill Clean PEI 225-235 60 50
Magnetic Iron PLA Clean PEI 220-230 60 50
Stainless Steel PLA Clean PEI 220-230 60 50
Conductive PLA Clean PEI 215-230 60 50
Coee PLA Clean PEI 220-230 60 40
nGen Clean PEI 220-240 85 60
t-glase Glue stick 240-260 60 45
Flexible Filaments Glue stick 215-230 50 35
Nylons Glue stick 220-270 110 50
Polycarbonate Glue stick 260-300 110 50
Polycarbonate + ABS Glue stick 260-280 110 50
INOVA 1800 Glue stick 235-255 75 50
n-vent Glue stick 225-245 60 50
Table 2.1: Recommended Temperatures
2.5 Removing Your First Print
After your rst print has nished, wait for the print surface to cool to
the recommended print removal temperature. Your parts will be easier to
remove if you allow your heated bed to cool down to optimal temperature.
This will allow the plastic to contract, making it easier to remove.
Once your heated bed has cooled, use the blue handled knife that was
included with your toolkit to remove the item. Carefully insert the blade
of the knife between your print and heated bed. Once underneath the part
rotate the blade lifting with the sharp edge into the part, to gently pop the
30
PROOF
Page 33
2.6. FULL SETTINGS
piece o your plate.
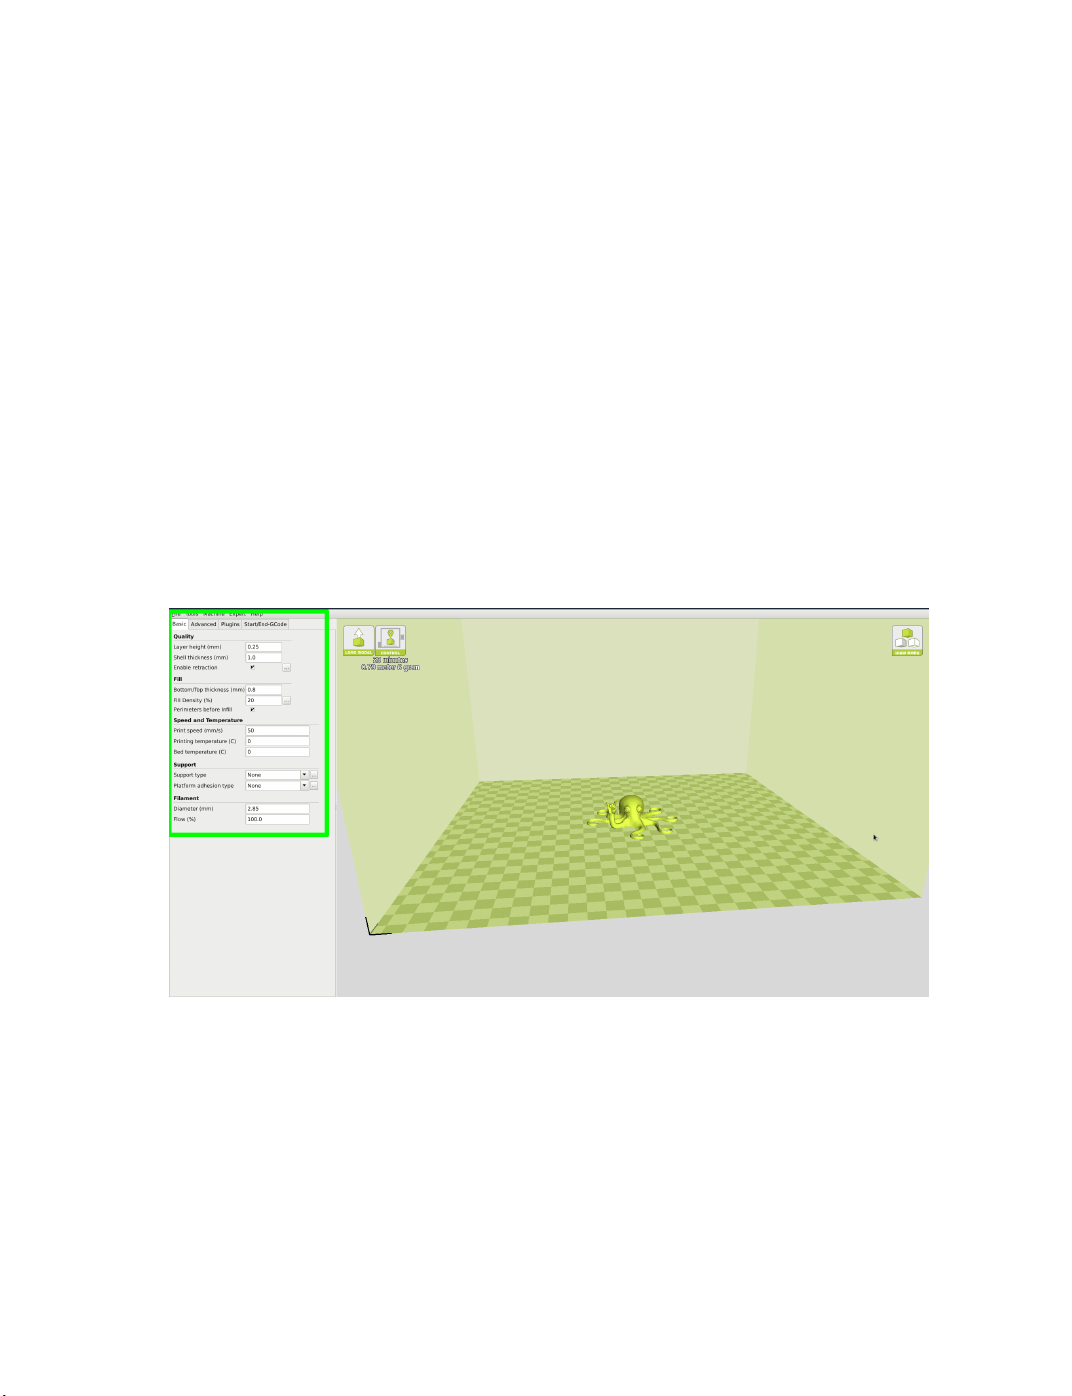
2.6 Full Settings
Full settings should not be used until enough experience with 3D printing
has been gained to feel comfortable with all aspects of the printer and its
operation. Quickprint Mode will provide good results for most models. The
rst time Cura is launched it will default to the Quick Print interface. In
order to have more control of your slicing and GCODE generation, switch to
Full Settings. Choose your desired Quick Print prole, as you can copy
over the current settings when changing to Full Settings mode. This
will automatically update the settings for that lament. Select Expert >
Switch to Full Settings. The following tabs will now be available: Basic,
Advanced, Plugins, and Start/End-GCODE. You will also have access to
the Expert Settings menu entry.
Figure 2.13: View in Full Settings
View in Full Settings
When you rst switch to Full Settings, Cura will need to know what
lament and quality you wish to use. It will automatically transfer our
31
PROOF
Page 34
Cura LulzBot Edition
quickprint settings over to allow adjustments if one is selected. IF A
QUICKPRINT PROFILE IS NOT AVAILABLE, YOU WILL NEED TO
MANUALLY LOAD ONE IN. We recommend using our tested proles
that are available here: https://www.lulzbot.com/cura. You will want
to choose the prole that matches your lament and quality needs. Once
downloaded, you can load the le into Cura by selecting File > Open
Profile. This will automatically update all of your Cura settings for use
with your specic lament.
2.7 Basic Tab Options
Layer Height
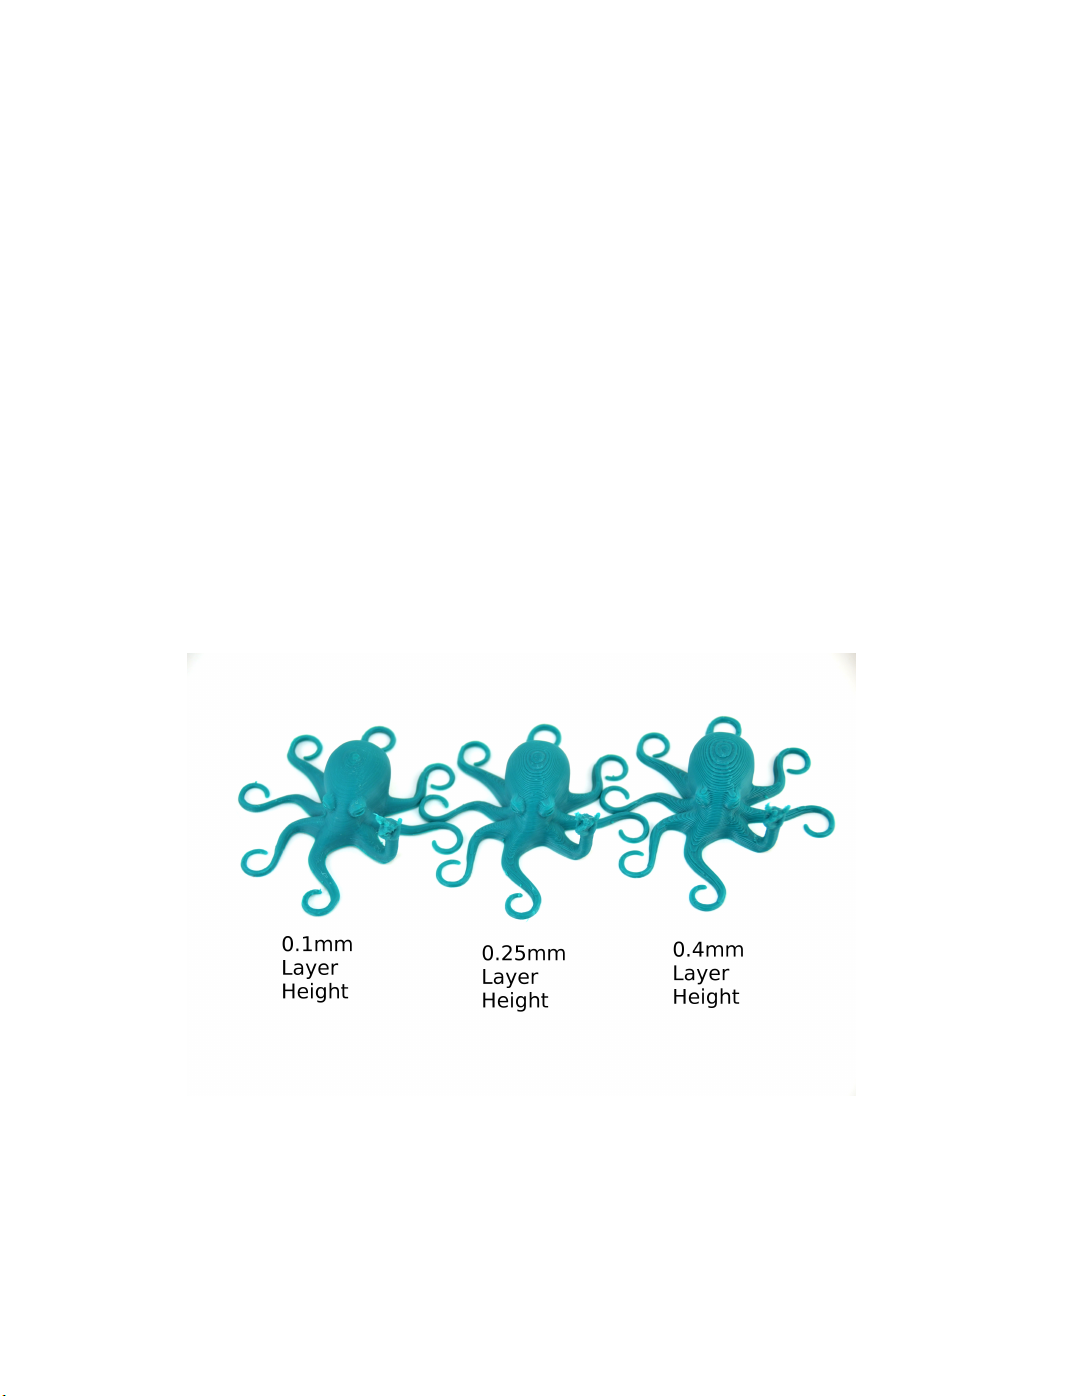
The thickness of each printed layer is known as the “Layer Height”. The
smaller the layer height, the smoother curves will appear. Larger layer
heights are better for bridging and overhangs. Smaller layer heights will
also increase print time, as it will take more layers to complete the object.
Figure 2.14: Dierences in Layer Height
32
PROOF
Page 35
2.7. BASIC TAB OPTIONS
Shell Thickness
This denes the number of vertical walls that comprise the outside of your
model. We recommend keeping this set to multiples of your nozzle width.
Your TAZ 3D printer is equipped with a 0.5mm nozzle.
Enable Retraction
Retraction tells your printer to pull lament out of the hot end upon travel
moves. Travel moves are when your print head moves from one area of the
print, to another without laying down lament. We recommend keeping
this on for all lament types, and adjusting the retraction length and speed
for the specic lament.
Bottom/Top Thickness (mm)
Also known as “Surface Layers” this will determine how thick the top and
bottom layers are. A larger number here will create a thicker top and
bottom which can be helpful for strength, bridging, and quality purposes.
We recommend keeping this number as a multiple of your layer height.
Fill Density
This number is expressed as a percentage. 0% will give a completely hollow
print, while 100% will give you a completely solid object. We have found
that 20% to 40% ll density is functional for most prints.
Perimeters Before Infill
This option will toggle the order in which the inll and perimeters will be
printed. We recommend leaving this on.
Print Speed (mm/s)
Your overall printing speed can be adjusted here. If no other speeds are
determined in the later sections your printer will automatically default to
this speed. This speed will be dierent, depending on what type of lament
you are using.
33
PROOF
Page 36
Cura LulzBot Edition
Printing Temperature
This is where you will set the hot end temperature for your specic material.
It will be preset when using the recommended quickprint proles. This can
be adjusted for ne tuning of dierent lament manufacturers to help layer
adhesion or stringing. See Recommended Temperatures Table: page 30.
Your hot end is capable of reaching a maximum temperature of 300°C.
Bed Temperature
This is where you will set the print surface temperature for your specic
material. These will be preset when using the recommended quickprint
proles. This can be adjusted for ne tuning of dierent lament manufacturers to help adhesion or release. See Recommended Temperatures Table:
page 30. Your print surface is capable of reaching a maximum temperature
of 125°C.
Support Type
Some models will require support material in order to print properly. This
will usually occur when an object has an angle in relation to the build plate
between 0 to 45 degrees. It is highly recommended to orient your object so
that it minimizes or eliminates the need for support.
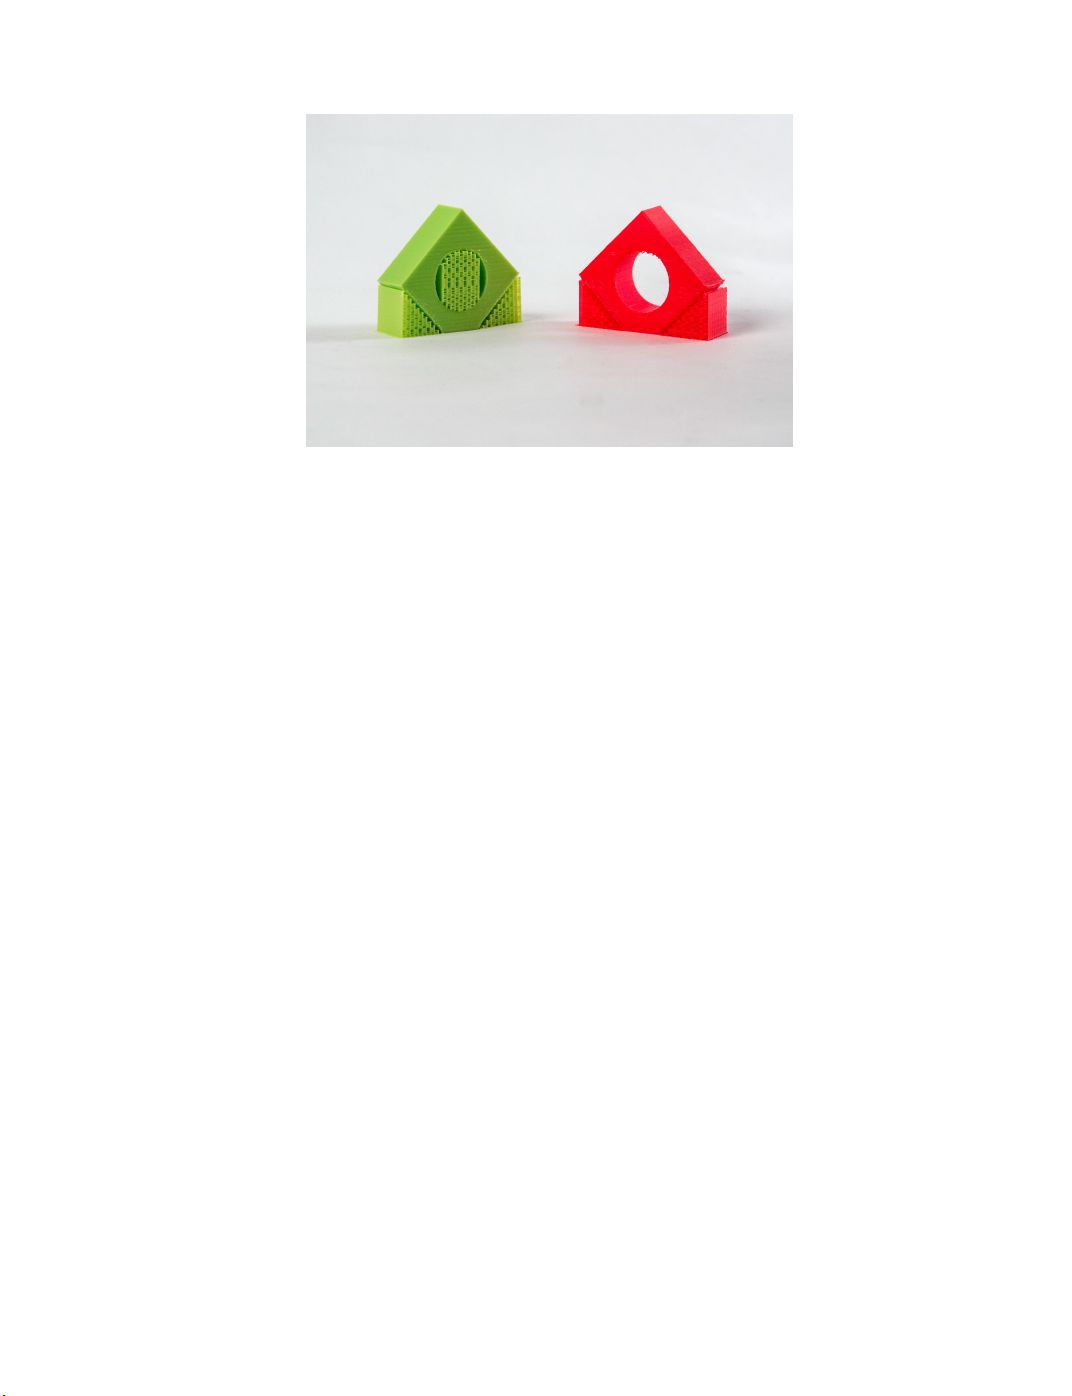
Touching Buildplate
This causes the support material to build up between the heated bed and
the object. The red example is Touching Buildplate.
Everywhere
This prints support material between the heated bed and object as well as
between the object and itself. The green example is Support Everywhere.
34
PROOF
Page 37
2.7. BASIC TAB OPTIONS
Figure 2.15: Support Types
Platform Adhesion Type
Some models have a small surface area contacting the plate. This can
create adhesion issues causing your part to pop o at some point during
the print. To x this, use either Brim or Raft. Raft is better used when a
model has small heated bed contact points and overhangs.
Brim
Brim will create a single layer of lament, contacting and surrounding your
model. This will increase the surface area of the part contacting the build
platform thereby preventing it from popping o the heated bed. Brim will
also help in situations where you are seeing corner lift. Brim settings can
be adjusted in the Expert Settings options.
Raft
Raft will generate a layer of material underneath your object. Raft was
more often used before the addition of heated plates to increase surface
area. Raft settings can be adjusted in the Expert Settings options.
35
PROOF
Page 38
Cura LulzBot Edition
Filament Diameter
The lament diameter setting is one of the more important settings. Make
sure that you update this value periodically with your average lament
diameter. While your lament may be referred to as 3mm, it is more
likely going to be near 2.9mm +/- 0.1mm. You will want this to be an
accurate average, as it will allow your printer to correctly calculate how
much lament it is pulling into the hot end. The default value should be
set to 2.85mm.
Filament Flow %
This controls how much lament your printer is extruding in relation to
speed. This setting is mainly used to adjust for lament density variations.
This may need to be adjusted when switching between dierent manufacturers or types of lament to adjust for die swell. It is recommended to
make small adjustments between prints for ne tuning.
2.8 Advanced Tab Options
Nozzle Size (mm)
This denes your nozzle size. The slicing engine uses this value combined
with your other settings to determine how quickly to feed lament into your
hot end. The TAZ ships with a 0.5mm nozzle standard.
Retraction Speed (mm/s)
Retraction Speed determines the speed at which your lament is reversed
out of the hot end for travel moves and when changing direction during
printing. We recommend keeping this set to less than 25mm/s to help
protect the gears.
Retraction Distance
Retraction Distance determines how much lament is pulled out of your hot
end on travel moves and when changing direction. You will want to adjust
this depending on temperature settings and lament type. Higher thermal
36
PROOF
Page 39
2.8. ADVANCED TAB OPTIONS
retaining laments such as PLA behave better with a longer retraction
distance. We have found anywhere from 1mm to 3mm is a good starting
range.
Initial Layer Thickness
This will control how thick your rst printed layer height is printed onto
the heated bed. A larger initial layer height is more forgiving and will help
rst layer adhesion. All of our standard proles have a 0.425mm initial
layer height. This eliminates the need for adjustments when switching
between laments. Your LulzBot TAZ automatic bed leveling system could
be aected if you change this from the standard proles. Adjust at your
own risk.
Initial Layer Line Width
This will control how wide your rst extruded lament path is for the initial
layer. A wider line width will help with bed adhesion. We have found 125%
to be a good starting place. For models with moving, printed in place
parts, a smaller initial layer line width is recommended. Your LulzBot
TAZ automatic bed leveling system could be aected if you change this
from the standard proles. Adjust at your own risk.
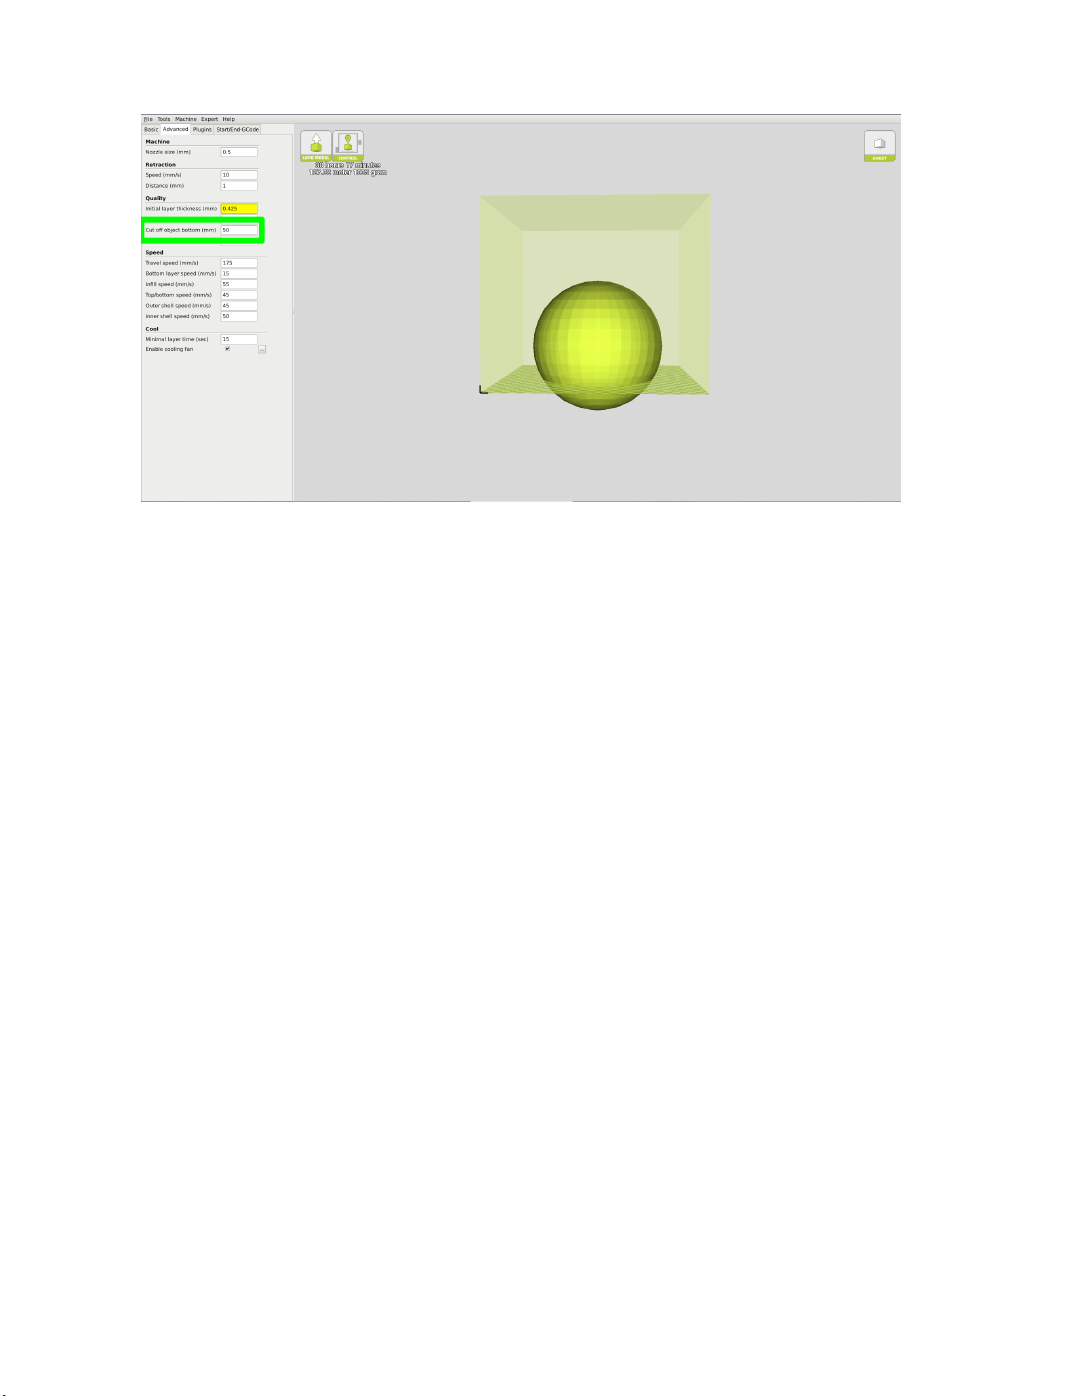
Cut Off Object Bottom (mm)
This setting is used to help print models that were not specically designed
for FFF printing. In particular, it is for models that do not have a at
surface to adhere to the plate. It will sink your object Xmm into the build
plate, creating a nice at surface to begin your print. You can also use this
option to remove the lower portion of your model, or if carefully measured,
cut your part in half for printing object as two halves.
37
PROOF
Page 40
Cura LulzBot Edition
Figure 2.16: Cuto Example
Dual Extrusion Overlap
This will determine how far your Dual Extruders will overlap when laying
down material. This will help adhesion between the two dierent colors or
types of lament. This setting is only used when the printer is equipped
with two hot ends and extruders.
Travel Speed
This setting will determine how fast your print head moves while not extruding lament. A normal travel speed of 125 - 175mm/s is recommended.
Bottom Layer Speed
This will control your initial layer speed. In general, a slower initial layer
speed will help with rst layer adhesion.
Infill Speed
This is how fast your print head speed will be while laying down the interior
portion of your model. Faster speeds are usually tolerable here, as none of
the inll will be visible from the outside of your object. If you go too fast
38
PROOF
Page 41
2.9. PLUGINS
compared to your inner and outer shells, you can have adhesion issues or
blobs of lament left behind from the print head.
Outer Shell Speed
This will be the outermost surface of the model. This is the most important
speed setting, as it controls the speed of your print head on the visible layers.
As a general rule of thumb, the slower you go the better looking print you
will get.
Inner Shell Speed
This aects vertical walls that are in between the outer shell and inll. This
will not be visible but will help support the outer shell and the inll. We
recommend keeping this speed setting between your inll and your outer
shell speed.
Minimal Layer Time
This will determine a minimum amount of time your printer will spend
laying down each layer. If your layer print time falls below this your printer
will automatically slow down to reach this time before moving onto the next
layer. Tweaking this can help get cleaner, crisper prints.
Enable Cooling Fan
Enables operation of your extruder active cooling fan. The fan settings can
be adjusted in the Expert Settings options.
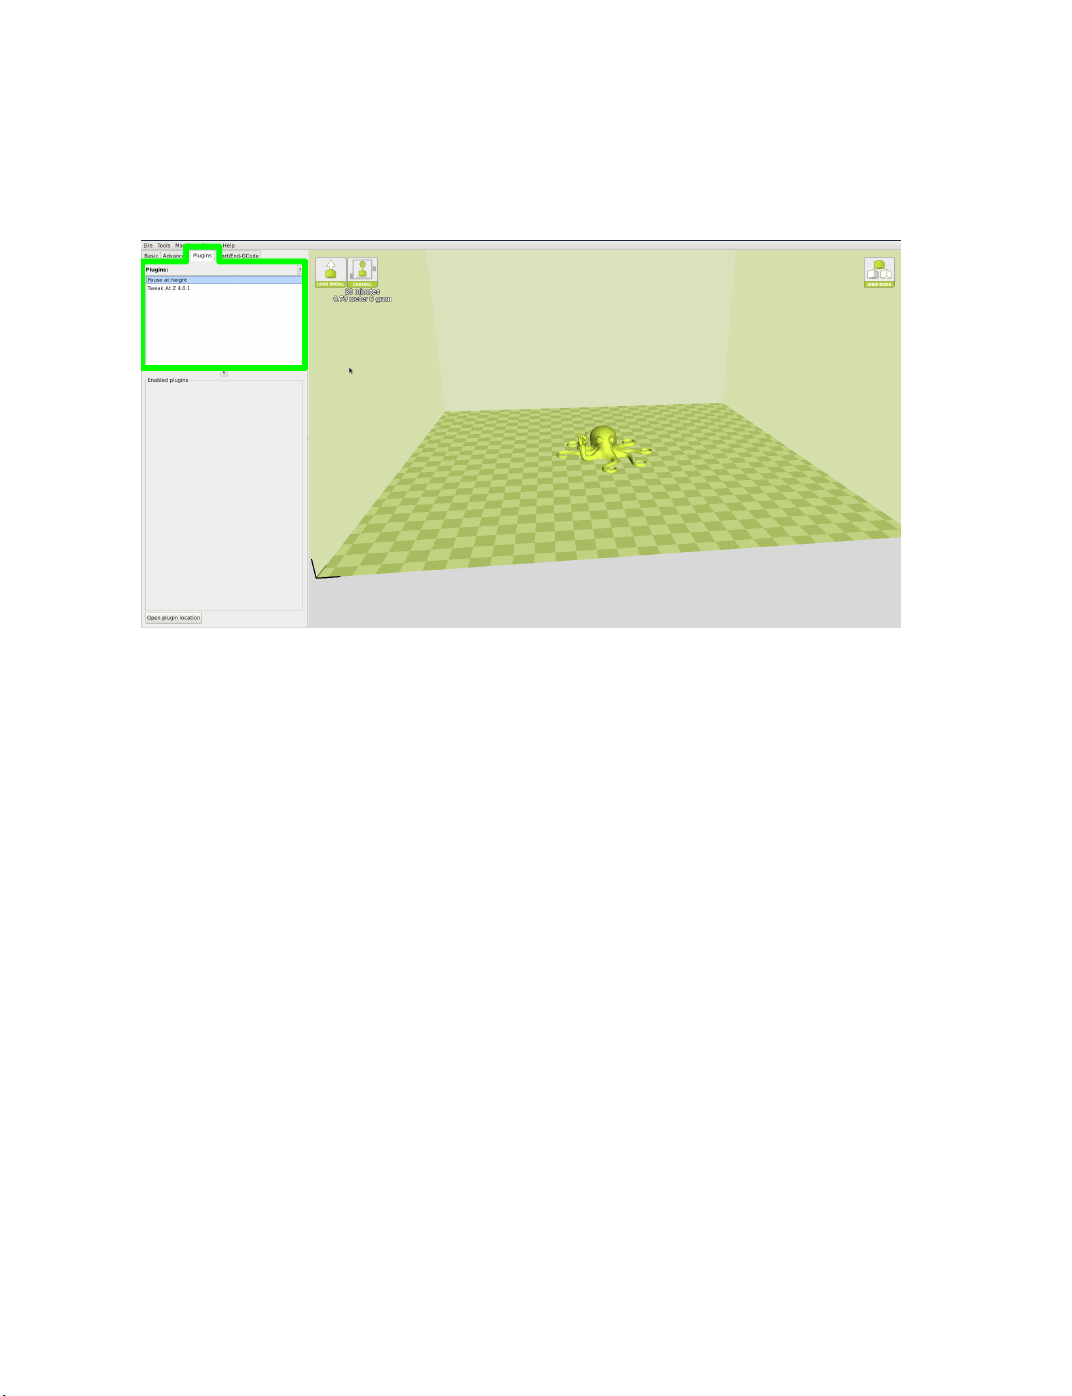
2.9 Plugins
Plugins are custom settings which will alter your print at specic
points. The two that come preloaded with Cura are Tweak at Z, and
Pause at Height. More plugins and information can be found here:
http://wiki.ultimaker.com/Category:CuraPlugin To activate one of
these highlight the desired plugin and click the drop-down arrow directly
below the Plugins box. These plugins aect how GCODE is generated. Use
39
PROOF
Page 42
Cura LulzBot Edition
at your own risk. Be sure to turn these off before switching back
to quick print mode. They will affect quickprint settings if
left on.
Figure 2.17: View of Plugins
Tweak at Z
Make basic changes at specied Z heights. You can dene the Z height or
layer count at which you want to make a change. Then choose how you
would like to change your settings. You can alter temperatures, fan speeds,
and print speeds. Fine tuning these for specic STL les, can produce
cleaner prints.
Pause at Z Height
Pause your print at a specied height. You can also specify where to
move the print head and how much lament to retract. This will prevent
“blobs” from accumulating on your print while paused. This setting is most
commonly used when switching colors of laments in the middle of a print.
40
PROOF
Page 43
2.10. START AND END GCODE SETTINGS
2.10 Start and End GCODE Settings
Custom GCODE allows for complex automatic printer movements and
operations. By adding custom GCODE into the start or end of your le, you
can alter how it prints. A comprehensive list of GCODE commands can be
found here: http://reprap.org/wiki/G-code We recommend new users
to leave this as provided in the proles at https://www.lulzbot.com/cura
TAZ 6 Specific Considerations
Please be cautious when changing any of these start and end GCODE
settings. This is where your automatic bed leveling commands are stored.
If improperly altered, your printer will no longer automatically compensate
for the heated bed position and can potentially damage components on
the printer. If you are uncertain of the change you are trying to make
to start/end GCODE, please contact us at [email protected] before
hand.
Changing Wiping and Probing Temperatures
We have set wiping and probing temperatures that we have found work
well with specic types of lament and lament manufacturers. If you are
using a type and/or manufacturer of lament not listed in the quickprint
settings, you may need to adjust these temperatures for optimal probing.
In the start GCODE section, there will be three separate temperatures you
can adjust. What these GCODE lines do will be described in the green
text to the right of the command. The ones you will want to adjust are:
• M109 SXXX ; soften lament for z homing
• M104 SYYY ; wipe temp
• M109 SZZZ ; heat to probe temp
By changing the variables (XXX, YYY, ZZZ), you can change what
temperature your printer will soften, wipe, and probe. Our temperatures
for softening, wiping, and probing will be a good starting point for other
manufacturer’s lament. When making adjustments, we recommend +/-
5°C changes at a time. Be sure to watch the probing sequence when
41
PROOF
Page 44
Cura LulzBot Edition
experimenting with new temperatures. Be prepared to power o the
3D printer if the probing sequence fails.
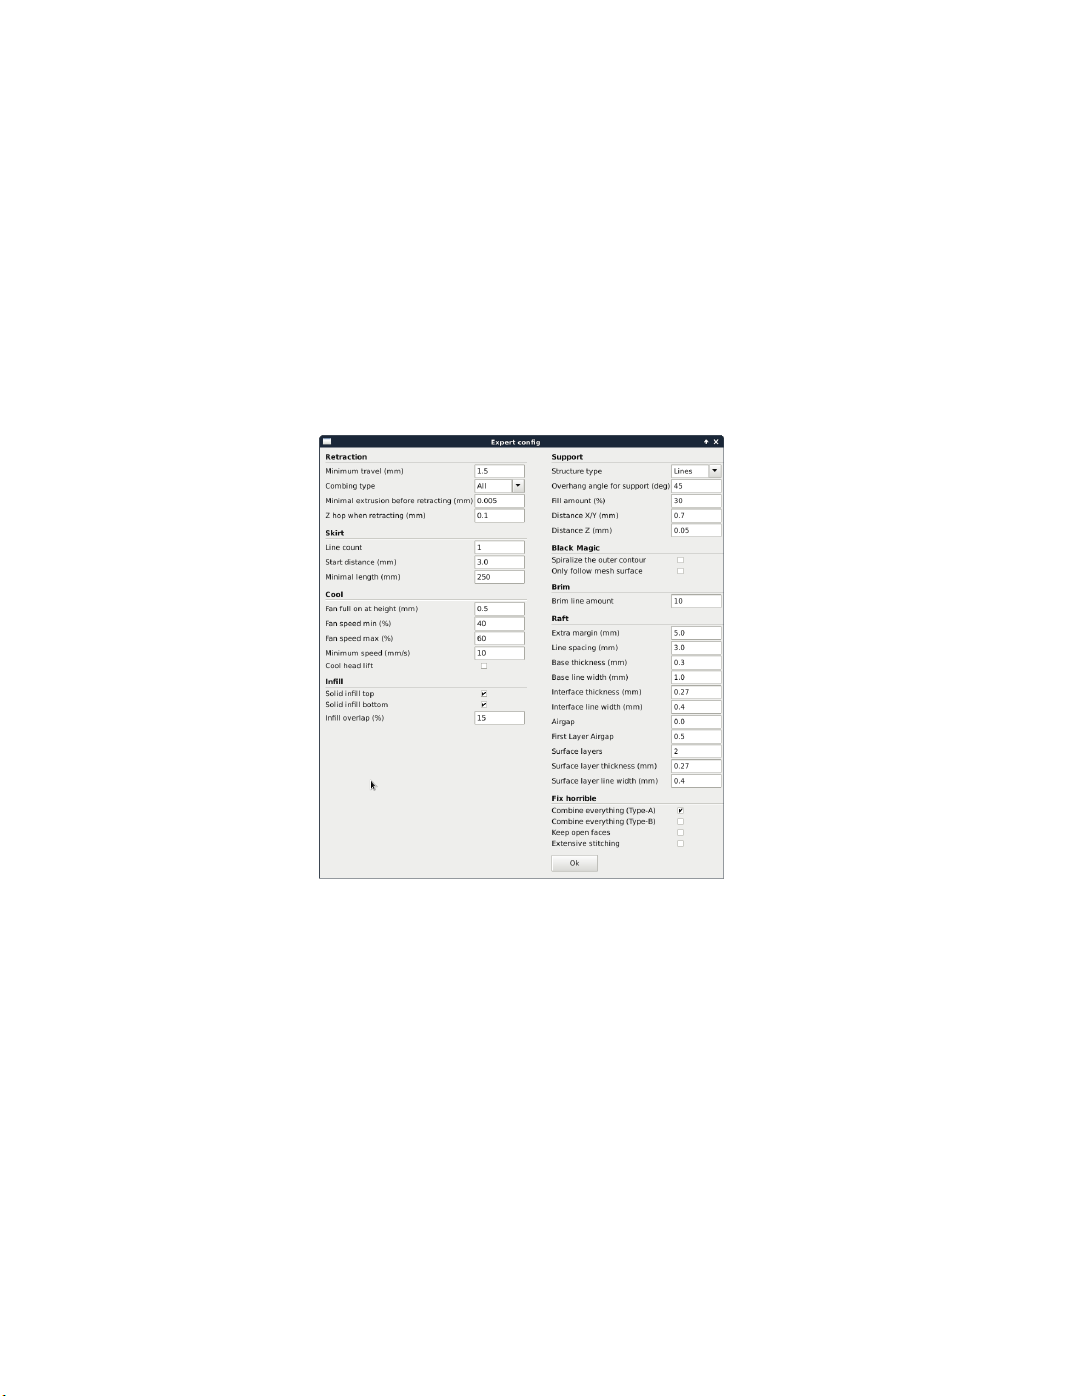
2.11 Expert Settings
Expert settings will give you more specic options for your retraction, skirt,
active cooling, inll, support, brim, raft, and special settings. To gain
access to this section you go to Expert > Open Full Settings or on your
keyboard press Control + E.
Figure 2.18: View Expert Settings
2.12 Retraction
Retraction pulls lament out of your nozzle when it is not extruding to
prevent your print head from dripping on your object. This section is
where you will control how your extruder retracts its lament.
42
PROOF
Page 45
2.13. SKIRT
Minimum Travel
This sets the minimum travel distance of your print head in order to retract.
If your print head is not moving this far during travel moves, it will not
retract.
Combing
This option prevents your print head from traveling over holes in the
X/Y plane when printing. This will slightly increase print time, but will
prevent strings from getting caught on the holes during travel moves. We
recommend keeping this setting on.
Minimal Extrusion Before Retracting
This will prevent a retraction move, if your extruder has not put out Xmm
of lament since its last retraction.
Z Hop When Retracting
This will raise your print head Xmm while retracting. This setting helps
prevent ooze and strings from being deposited on your print.
2.13 Skirt
Skirt creates a line around the outside of your object. Most commonly used
to prime the extruder, in order to prevent missed lament at the beginning
of a print. Leave this setting on. Turning this setting o will allow for
utilizing the full build volume.
Line Count
This will dene the number of loops the Skirt creates around the outside
of your object. Smaller models will require more loops to properly prime
the extruder.
43
PROOF
Page 46
Cura LulzBot Edition
Start Distance
This will dene the distance away from your model that the skirt will be
created.
Minimal Length
This will dene the minimum extruded line length for the skirt. This will
over ride your line count, producing as many lines as required to reach the
minimal length.
2.14 Cool
This section will dene how your extruder cooling fan will operate during
the print. If your print speeds are slowed down due to minimal layer time,
the fan will run between minimum and maximum speed based upon how
much the layer is slowed down.
Fan on at Full Height
This is your Z height where your fan will be turned on to its minimum
percentage setting. Especially helpful with high temperature retaining
laments such as PLA. This will be scaled between 0%, and your minimum
fan speed based upon layer height; with it being disabled for the rst layer.
Fan Speed Min
This will be the speed your fan runs when enabled at full height. Once the
Z height is reached for Fan on at Full Height, this will be the speed your
fan runs at.
Fan Speed Max
This is the fastest speed at which your fan will ever run. When your print
speed is slowed down due to minimal layer time, your fan will run between
minimum and maximum speed. The maximum fan speed is reached when
your printer must be slowed by 50% or greater.
44
PROOF
Page 47
2.15. SUPPORT
2.15 Support
You dene how your support material is generated here. You must have
some form of support turned on in the basic settings in order for these
settings to have an eect.
Structure Type
You can choose between a Grid or a Line pattern for your support material.
The grid will be a checkerboard pattern in the X and Y direction. The
line option will produce lines in along the Y-axis for support. The grid
will provide stronger support than the line option, but will be harder to
remove.
Overhang Angle for Support
This will determine where support material is generated. In general you
will be able to print a model with 45 to 90 degree angles in relation to the
bed without support. We recommend leaving this setting at 45 degrees.
Fill Amount
This will determine how dense your support material is printed, similar to
Inll Percentage. The higher percentage, the better support, but it will
be harder to remove the support material, will use more material, and will
lead to a larger total printing time.
Distance X/Y
This will determine how far away from your object in the X/Y plane that
the support material is being placed.
Distance Z
This will determine how far away your support material is from your object
in the vertical direction. A smaller number here makes for better support,
but makes it harder to remove.
45
PROOF
Page 48
Cura LulzBot Edition
2.16 Black Magic
This section allows you to transform your model into a hollow shell, a single
layer thick.
Spiralize the Outer Contour
This causes your Z-axis to be constantly moving upward as printing your
single outer wall shell. The results are no layer change lines, giving a much
smoother surface. This setting is typically only used for artistic objects as
they will be fragile.
Only Follow Mesh Surface
This will cause your print to follow the outside of your model, building
it completely hollow with a single wall outer shell. The only dierence
between this and Spiralize, is that the Z-axis moves regularly. That is, it
prints a layer and then moves up vertically to the next one.
2.17 Brim
Brim circles the base of the print while making contact, helping adhere
the print to the heated plate. This is only one layer thick, and easily
removed post-print. This section denes how the brim is formed when
brim is activated in basic settings.
Brim Line Amount
This will determine the distance the brim will cover around the outside of
your object. The more brim used, the better your part will adhere to the
plate.
2.18 Raft
Raft is a platform built underneath your object, designed to help adhesion
and prevent warping. It will lay down support material, and then a
platform on top of the supports. Your model will be built on top of this
46
PROOF
Page 49
2.18. RAFT
platform. The bottom surface of your printed part will not be as clean or
as even when using this option. Raft is typically not required.
Extra Margin
This determines the distance around the outside of your object that the
raft is created. Can be helpful for ensuring no warping of the lower layers.
Line Spacing
This will determine the spacing between “support” lines for the raft. A
small spacing makes the support structures closer together improving
strength of the raft, but uses more material.
Base Thickness
This denes how thick your raft will be.
Base Line Width
This will dene how wide your “support” material is for the raft. This
setting will determine how well the surface layers of the raft print.
Interface Thickness
This will determine how thick the surface layers of the raft are. The surface
layers are the platform that is built upon the supports.
Interface Line Width
This will determine how wide the top layers of the platform will be. In
general, you can keep this set to your nozzle size, as surface quality of the
removable raft is not important.
Airgap
This will dene the distance between your raft and your print. A larger
gap will make your part easier to remove, but will make the bottom of your
47
PROOF
Page 50
Cura LulzBot Edition
print look worse.
Surface Layers
This will determine the number of layers that create the “platform” of your
raft. If you have a wide line spacing, you may want to increase this number
to ensure a solid platform.
2.19 Fix Horrible
These are some of the more advanced and experimental options. They are
designed to help repair models with errors to make them suitable for 3D
printing. They do not always work. Please be cautious when using these
options as they can have unintended eects on your print quality.
Combine Everything (Type-A)
This will attempt to x all external mesh errors, while keeping internal
holes intact. This can accidentally ll in intentional internal holes.
Combine Everything (Type-B)
This will ignore all internal holes of the model and only focus on the external
holes. This is helpful when only the outside nish of the model is important.
Keep Open Faces
This will ignore all manifold errors in the object. It can create issues
generating the GCODE as Cura does not know how to interpret the open
holes. This option should only be used if you are sure that the holes in the
mesh are intended. In general, you should not use this option.
Extensive Stitching
This causes Cura to automatically add triangle meshes in an attempt to x
manifold errors. This algorithm will greatly increase GCODE generation
time and may end up adding in un-intended meshes. It is recommended
48
PROOF
Page 51
2.20. DUAL EXTRUSION
that you repair your model through MeshLab, FreeCAD or your preferred
CAD program before attempting this option.
2.20 Dual Extrusion
The LulzBot TAZ has the ability to add dual extrusion functionality with
the Dual Extruder Tool Head. We only recommend the Dual Extruder Tool
Head for advanced users. Installation and operation of the dual extruder
will require you to ash your rmware, calibrate your extruders, level two
heads to a single plane, dene extruder osets, and ne tune your slicing
prole. This can be a little overwhelming for new users. We recommended
that you have a couple of months of single extruder printing experience
before making the switch.
Tool Head Installation Instructions
Refer to appropriate Dual Extruder Tool Head Quick Start Guide for
the specic steps required to install and operate your new tool head.
Failure to follow the proper steps may result in damage to the tool head
or 3D printer. Installation and operating instructions are available at
OHAI.LulzBot.com/accessories. The following steps are only meant to
be an overview of the typical process.
Updating Firmware
In order to use the Dual Extruder you will need to update your rmware
to activate the second hot end.
• Power on your 3D printer and connect it to your computer through
USB.
• Select Machine > Machine Settings.
• In the top right-hand corner you will see a Change Tool Head button,
select this.
• Next you will need to select the proper hot end type. Please compare
photos with your existing tool head. Choose the correct hot end and
select Next.
49
PROOF
Page 52
Cura LulzBot Edition
• Select the photo that corresponds with your tool head and press Next.
• The nal step will be flashing the firmware. Choose Flash the
firmware to be sure to update the printers rmware to the proper
settings. This must be done to allow your printer to operate properly.
• Once the progress bar has completed select OK > Next > Finish.
• You can verify a proper rmware update by looking at the LCD screen.
You should now see three separate temperature readings.
You can revert the rmware back to the stock conguration for your
LulzBot 3D printer by selecting Machine > Machine Settings > Change
Tool Head. Doing so will overwrite any of your current rmware settings.
Calibrating Extruders
Each individual extruder will have its own unique set of Extruder steps
per unit, or Esteps. Your Dual Extruder was calibrated before leaving the
production oor. The number for each extruder will be located on the
back of the tool head. This will need to be updated within your printer’s
rmware.
• Update your Esteps for the rear extruder and E1steps for the front
extruder through your LCD screen. Configuration > Advanced
Settings > E/E1 Steps > New Number. Push in on the knob to
exit out of the Esteps entry.
• Store your new Esteps Configuration > Store Memory.
Defining Second Extruder Offset
To get crisper looking prints, you will want to really dial in your osets.
With the outer and inner square on your build platform, left-click
on the outer square, then right-click on the inner square and select
Dual Extrusion Merge. The red square will be printed with your front
extruder, and the yellow square will be printed with the rear extruder.
50
PROOF
Page 53
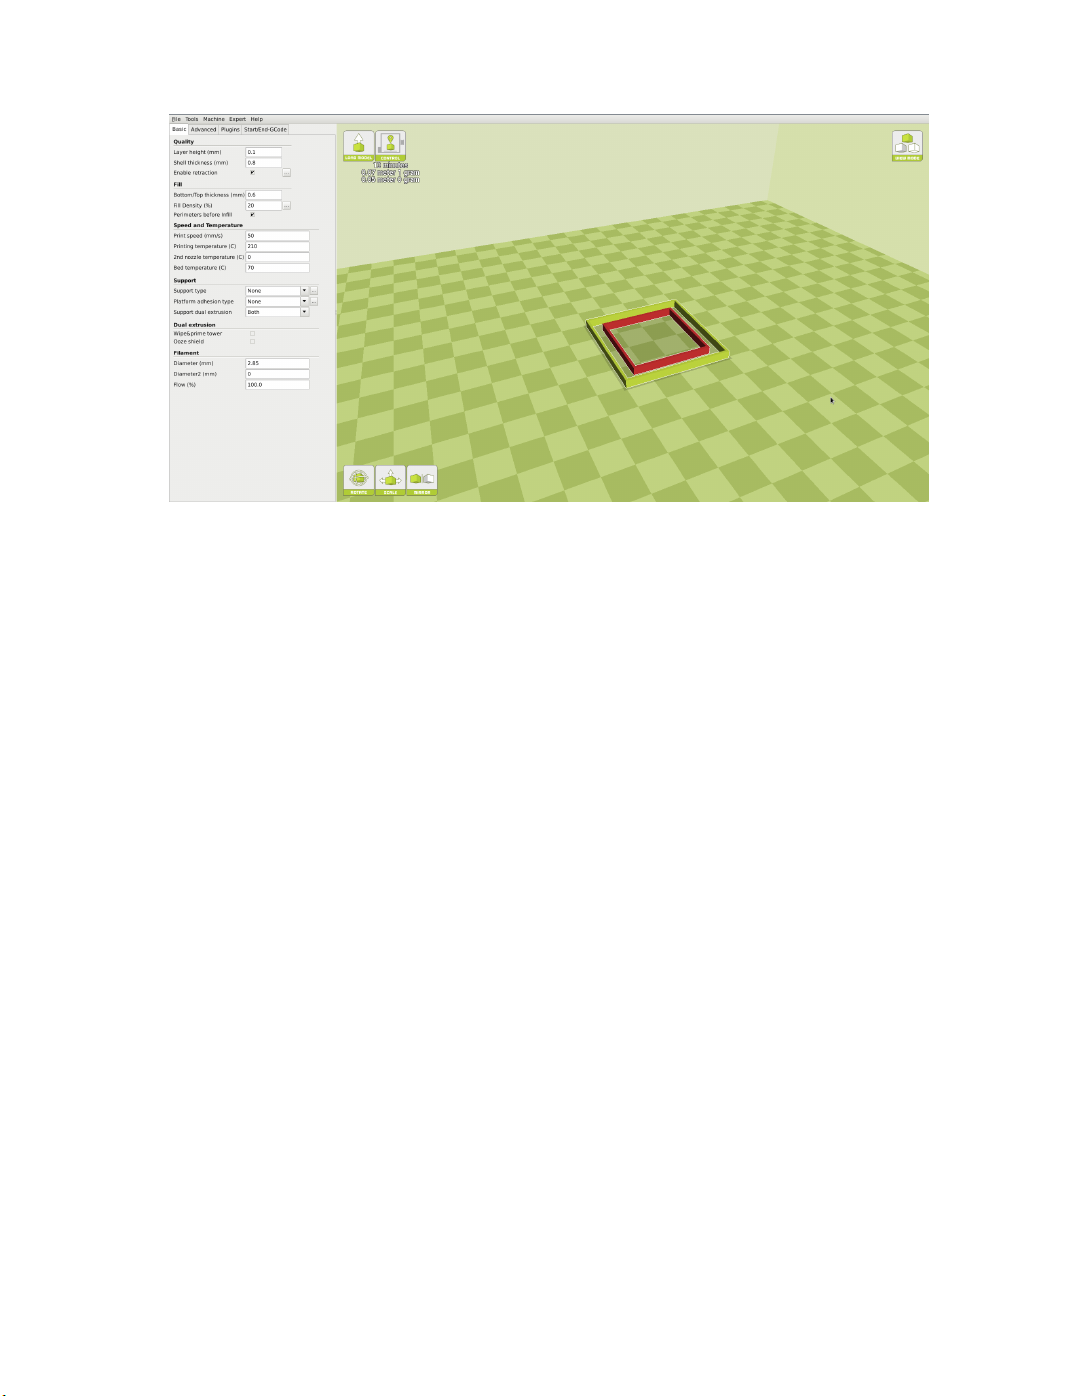
2.20. DUAL EXTRUSION
After printing the squares, you will want to measure Top, Bottom, Left,
and Right gap. Enter these numbers into our oset calculator found here:
https://www.lulzbot.com/dual-extruder-calibration-calculator
This will produce new osets, that will need to be updated in the Machine
Settings menu. Repeat as many times as desired to truly ne tune the
oset.
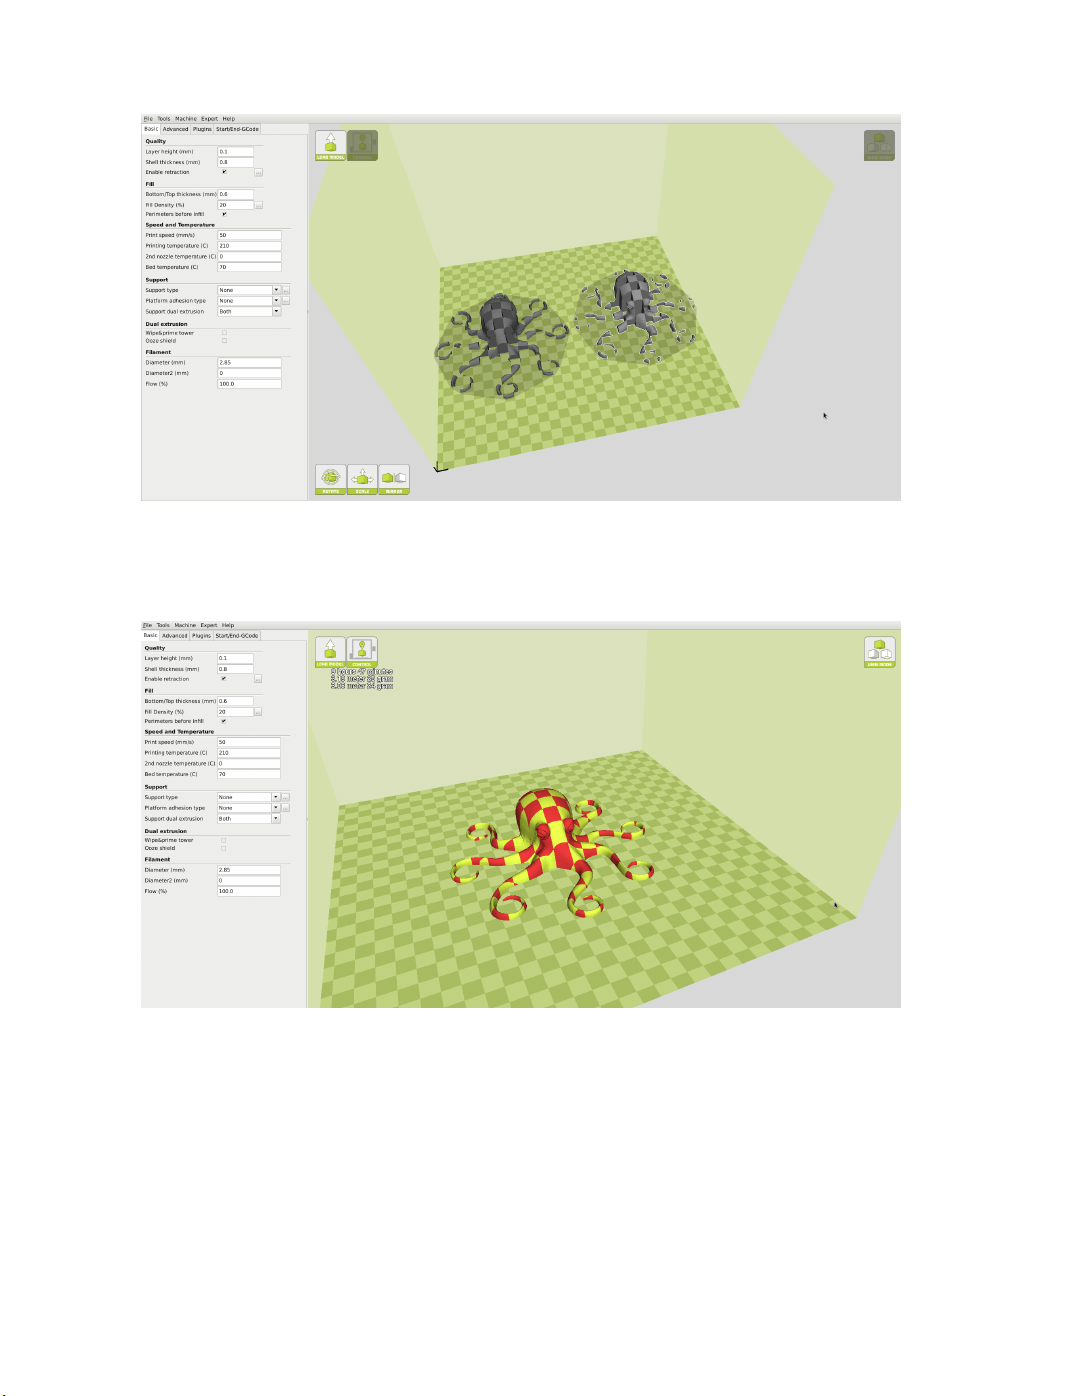
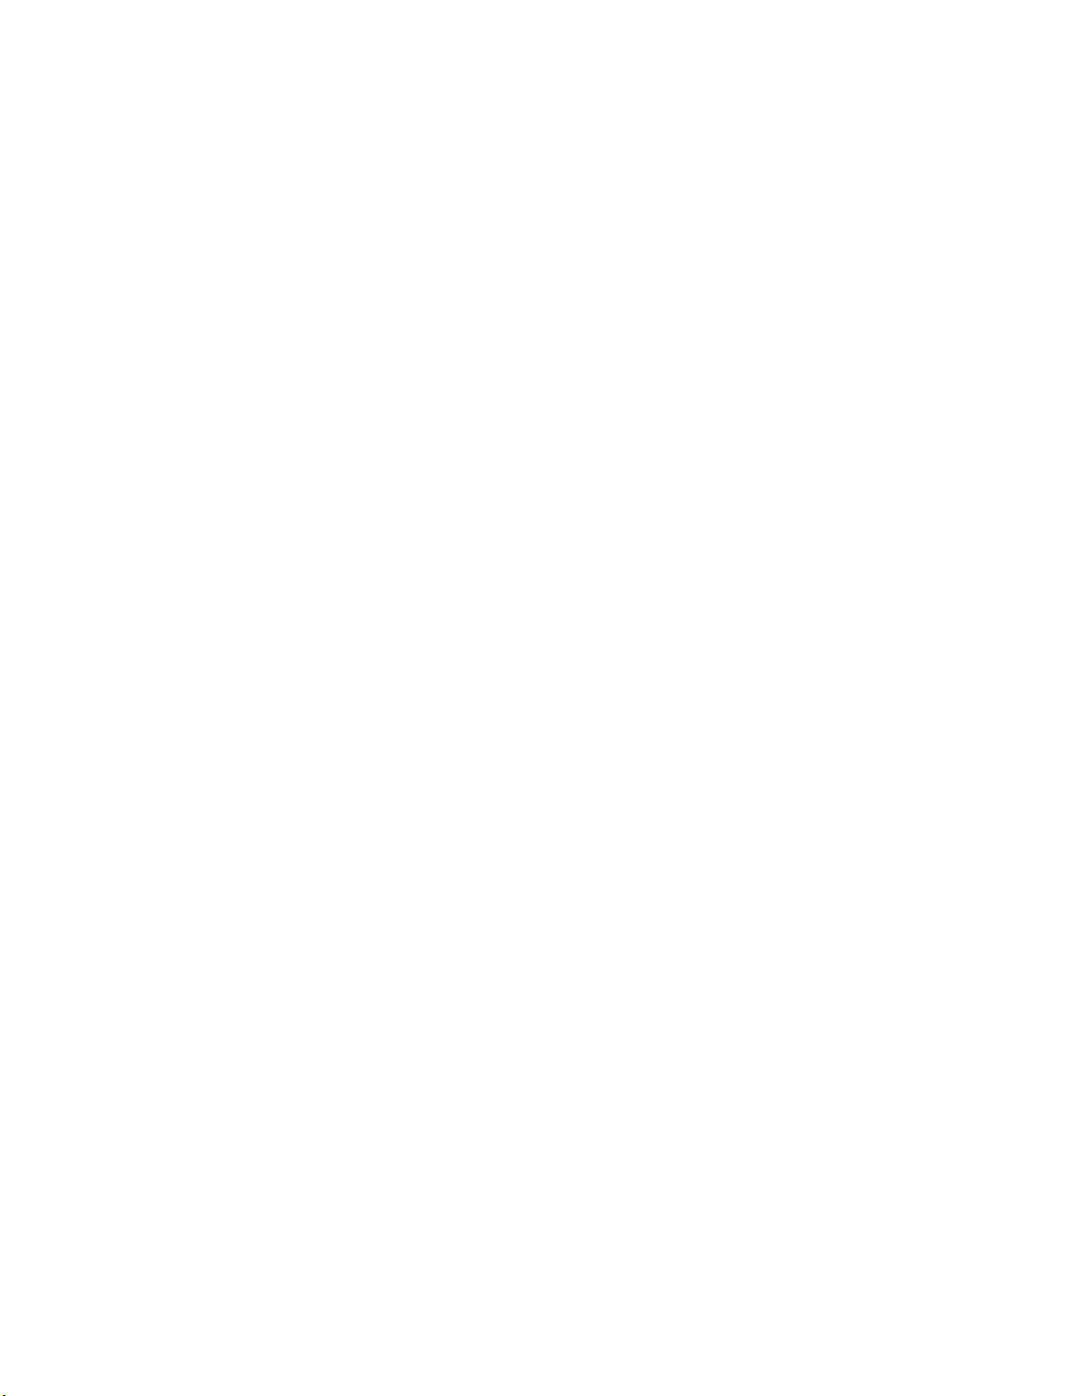
First Dual Print
When you are ready to produce your rst dual extrusion print, you will
need to combine the two separate STL les. One STL le will be for each
print head. Left Click on whichever STL you would like printed with the
Rear Tool head. Then Right Click on whichever STL le you would
like printed with the Front Tool head and select dual extrusion merge.
You will now see a single model in two colors on the build plate. The red
section will be printed with the front extruder, while the green section will
be printed with the rear extruder.
51
PROOF
Page 54
Cura LulzBot Edition
Figure 2.19: Before Merge
Figure 2.20: After Merge
First Print
After your object has been merged as intended, you will be ready to start
the print. After selecting print from your SD card or the control panel,
52
PROOF
Page 55
2.20. DUAL EXTRUSION
your printer will start the probing and cleaning process. It will clean both
nozzles, but only probe with the rear. If you are getting contact with your
printer nozzles on previous printed parts, you will need to level the front
hot end to the rear.
53
PROOF
Page 56
PROOF
Page 57
Printing with the Graphic LCD
PROOF
Page 58
Printing with the Graphic LCD
The Graphical LCD Controller, or GLCD, allows you to print with the
LulzBot TAZ 3D printer without needing to have a computer connected or
using host software such as Cura LulzBot Edition. This will allow for more
ecient space in the workspace and free up a computer for other tasks.
In the following sections you will nd general information on using the
GLCD, how to transfer .gcode les to the included SD card, heat up the
printer, start a print, and make conguration adjustments.
3.1 Graphical LCD Controller, Cura or
Other Host?
The Graphical LCD Controller is perfect for normal day to day printing
and will be used in the majority of your print jobs. However, in some
instances, you will want to use Cura instead of the GLCD. A few examples
of when you would want to plug the USB cable back in and use Cura:
• A number of manual movements are required to perform calibration
checks. Because of this it is easier and faster to make the required
manual movements within Cura. Calibration checks can be done with
the GLCD, but require a number of repetitive menu selections.
• Cura is the preferred printer host software, as the inclusion of quick
print proles, the combination of slicing engine, and printer host
communications allows for easy all-in-one use.
3.2 Multiple Connections
Because the LulzBot TAZ 3D printer can be controlled by the GLCD and
by host software, caution is advised when connecting to the printer through
USB as the print can be interrupted when connecting or disconnecting the
USB cable. A general rule is: once you have started a print with either the
GLCD, Cura, or another printer host, for the rest of the print use only that
controller. When printing with the GLCD, never try to connect through
USB in the Cura host software; wait until the print is complete, and then
connect in Cura.
56
PROOF
Page 59
3.3. PUTTING PRINT FILES ON THE SD CARD
3.3 Putting Print Files on the SD Card
To print from the GLCD, transfer .gcode print les onto the SD card. Follow
the normal steps, as explained in the Cura chapter, to create .gcode print
les on your computer. Insert the SD card into your computer using a SD
reader slot or USB SD card reader. Open a le browser- / -manager and
locate the created .gcode les; drag and drop or paste the .gcode les to
the SD card. Once the les have transferred, eject the SD card from your
computer and insert it back into the SD card slot on the left side of the
printer, at the top near the GLCD.
3.4 Printing With the Graphical LCD
Controller
The Graphical LCD Controller Status Screen
The GLCD screen will turn on you power up your LulzBot TAZ 3D printer.
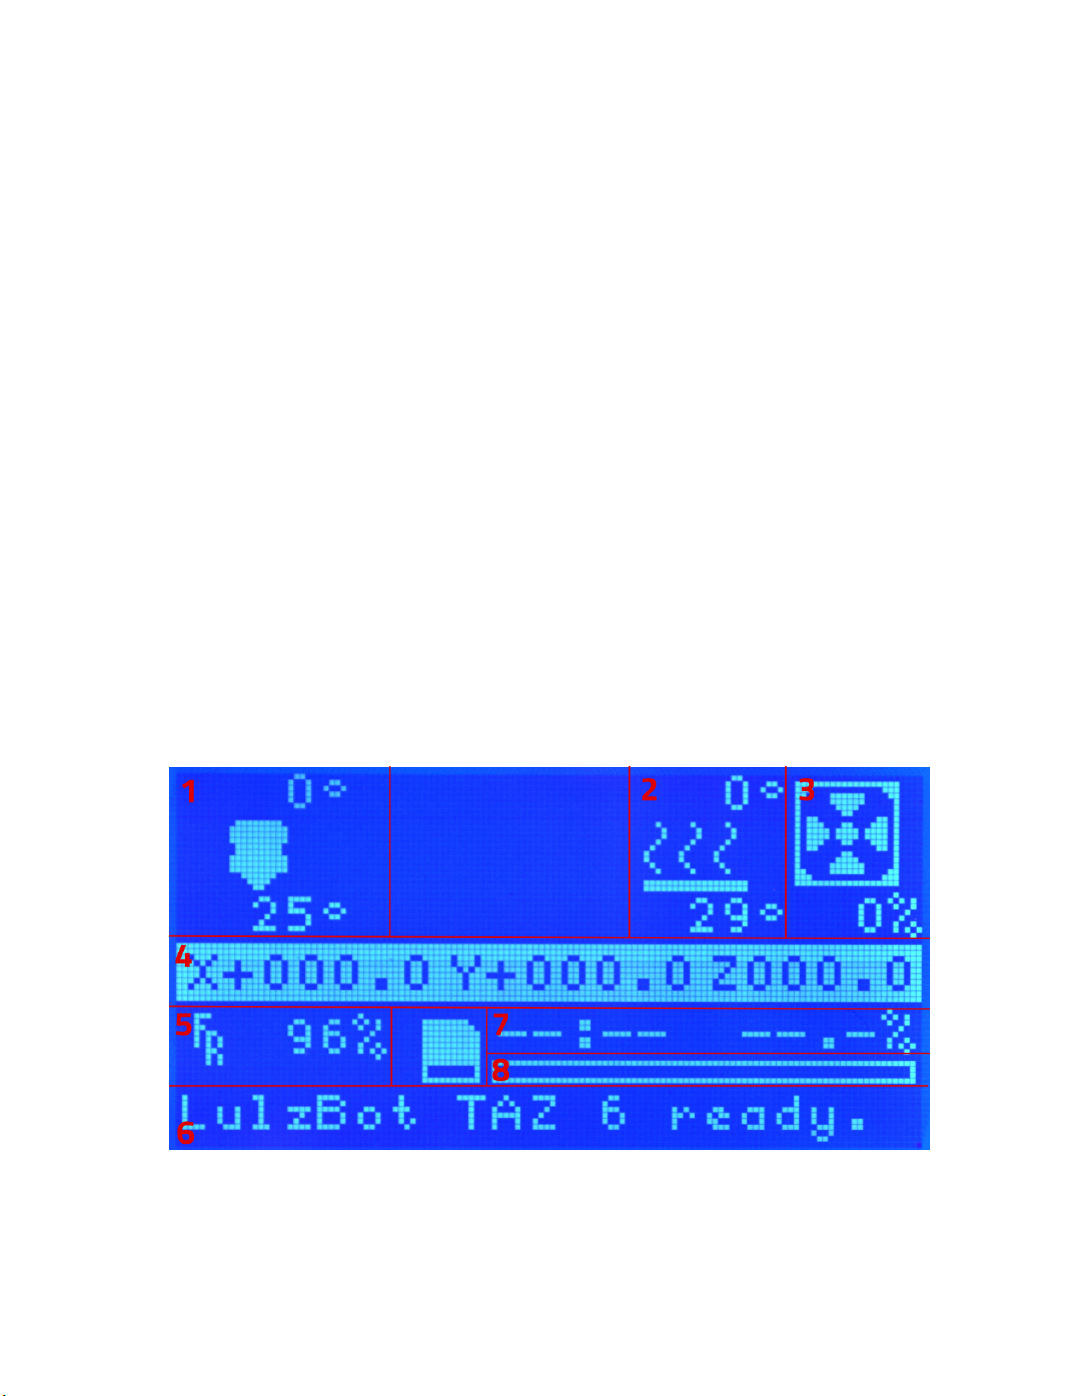
The start-up screen will display the Status screen (g. 3.1, page 57). The
Status screen is the default screen for the GLCD, presenting the current
status of the printer. There are a number of live statuses shown on
Figure 3.1: GLCD Info Screen
57
PROOF
Page 60
Printing with the Graphic LCD
the Status screen; these will give you current temperatures, tool head
coordinates, print status, and more. The dierent numbered sections of
the status screen are shown in Figure 3.1 above. Follow the key below for
more information on each section.
1. Hot end temperatures: represents the current temperature (bottom)
and set temperature (top) of up to three nozzles. The RAMBo control
electronics currently only supports two hot ends.
2. Heat bed temperature: represents the current temperature (bottom)
and set temperature (top) of the heat bed.
3. Fan speed: represents the current optional extruder fan speed. The
fan is set to o (0%) by default; the fan is not recommended for
ABS. If you print with PLA lament, you will want to use the fan. If
cooling is turned on in Cura, this portion of the display will change
to reect the .g-code embedded extruder fan control instructions.
4. Tool head coordinates: represents the current tool head coordinates
on the X, Y, and Z axes.
5. Feed rate: represents the current feed rate setting. The feed rate is set
to 100% by default; this matches the speed set in the gcode generation.
When on, the status screen selection knob can be turned to increase
or decrease the feed rate during the print. Increasing/decreasing the
feed rate will increase/decrease the speed of the print.
6. Printer status: lists the current status of the printer including: SD
card status, current printing le, or completed print time.
7. Current print time: lists the length of time for the current print job.
8. Progress bar: represents the progress of the current print job. The
print is nished when the bar is completely white.
Using the Selection Knob
To navigate through the GLCD menu use the selection knob by rotating
to scroll through selections and pressing the knob to make a selection.
From the main status screen, press the knob to move into the menu screen
58
PROOF
Page 61
3.4. PRINTING WITH THE GRAPHICAL LCD CONTROLLER
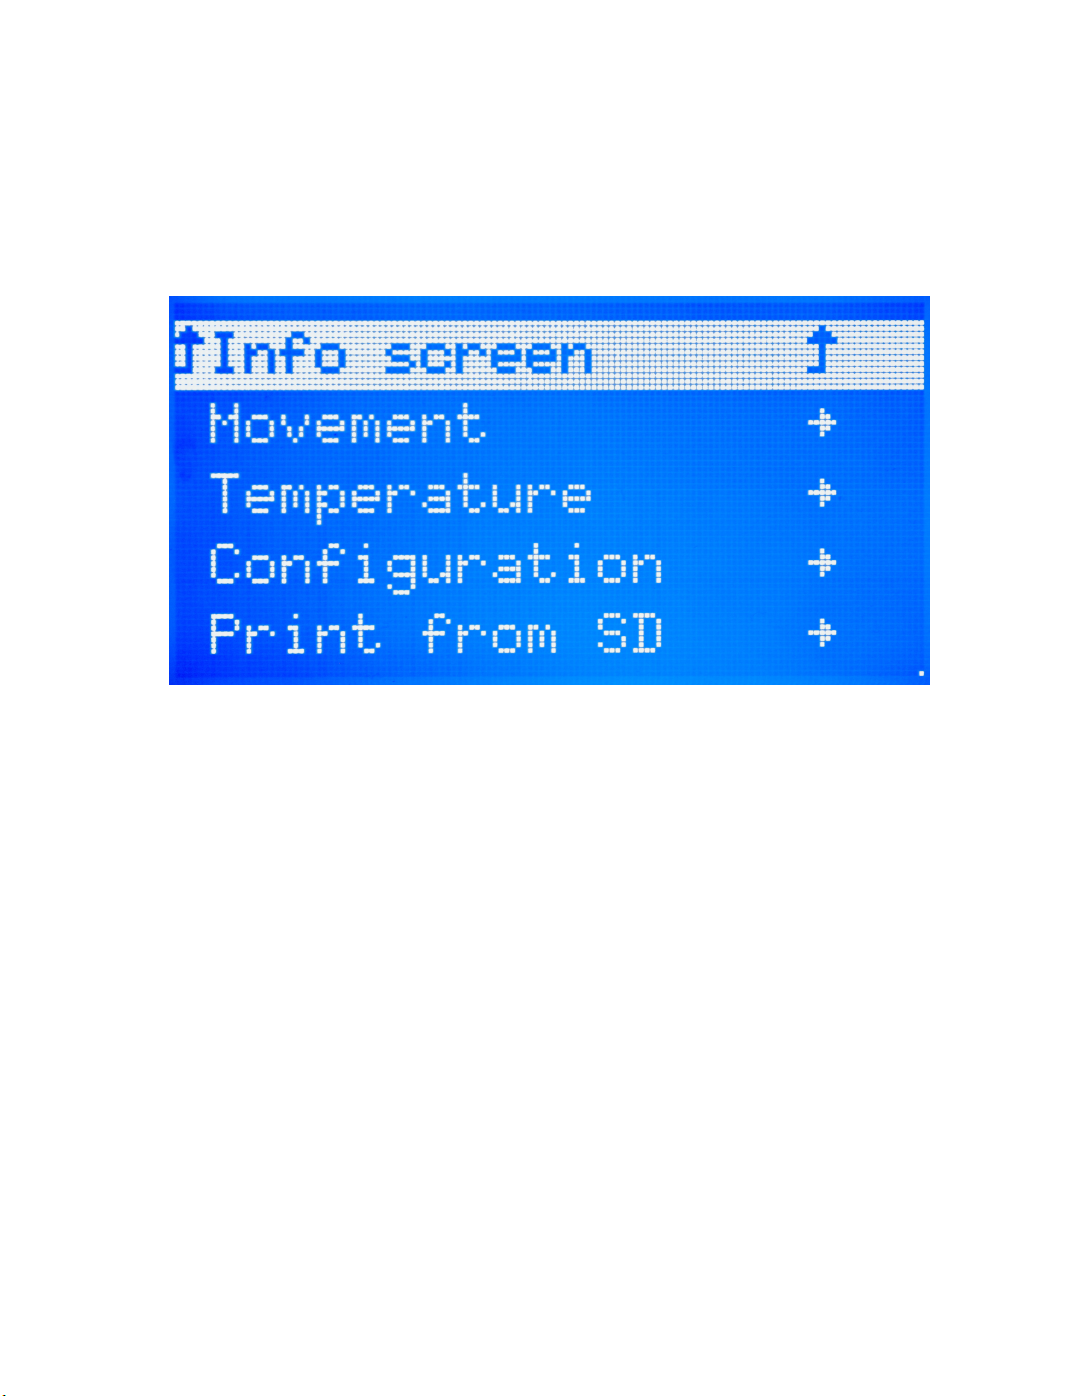
(Figure 3.2, page 59). To move backwards in the menu tree, select the top
most menu selection on the current screen. Selections that will move you
backwards through the menu tree are noted by an upwards-facing arrow.
Note that if the menu is left idle it will automatically move back to the
main status screen.
Figure 3.2: Main Menu
Selecting a File From the SD and Starting a Print
Once the SD card has the desired GCODE le loaded onto it, you can begin
your rst print. From the main menu select the Print from SD option.
You will now see a selection of the directories and .gcode les on the SD
card. Navigate through the menu to locate the le you would like to print.
Select the desired le to begin the print.
Making Manual Movements With the Graphical LCD
Controller
As noted previously (page 56), making numerous manual movements is
easier done using Cura. However, you can make manual movements with
the GLCD. Navigate to Movement -> Move Axis. You will select the length
59
PROOF
Page 62
Printing with the Graphic LCD
of the movement and then which axis to move.
When at the move screen; turn the selection knob clockwise to move
the axis in millimeters in the positive direction and counter-clockwise for
the negative direction.
Tune
Once you begin a print, you will notice your movement option changes to
tune. This section will allow you to make changes to individual settings
while a print is running. You can adjust overall speed, nozzle temperature,
bed temperature, ow %, check apprx layer height, and even change
lament. When adjusting these settings, we recommend making
small changes at a time.
Change Filament
You can change lament through the GLCD mid print by going to Tune
-> Change Filament. This will park your print head in the front left
corner, and wait for you to resume the print. During this time you can
change colors, or even types of lament. Once your lament change has
completed, press in your GLCD knob to continue where it left o. If
you manually move the tool head while changing filament, your
printer will lose place of it's position.
3.5 Configuration Options
Out of the box, the LulzBot TAZ 3D printer is already calibrated for
printing. However, the GLCD does allow tuning of the more advanced
conguration settings. We highly suggest you not modify the conguration
settings unless you are certain it is necessary. The conguration section
contains settings that control how your printer operates.
Changing EEPROM Settings
The Store Memory and Load Memory functions will store and load the
changes you make using the GLCD. You must use the Store Memory
function to save the adjusted settings when the printer is powered on. If you
60
PROOF
Page 63
3.6. ADVANCED SETTINGS
ever need to revert to the original factory settings navigate to Control ->
Restore Failsafe. Clicking Restore to Factory will set all conguration
settings back to the original factory settings in the rmware.
For more information on the conguration settings please see the
LulzBot TAZ support page at LulzBot.com/support.
3.6 Advanced Settings
In the advanced settings, you can control/modify your Z oset, maximum
velocity, acceleration, jerk, and esteps/mm. Once again we highly suggest
you not modify the conguration settings unless you are certain it is
necessary. Making incorrect adjustments of these settings can have adverse
aects on your prints, and potentially damage your machine.
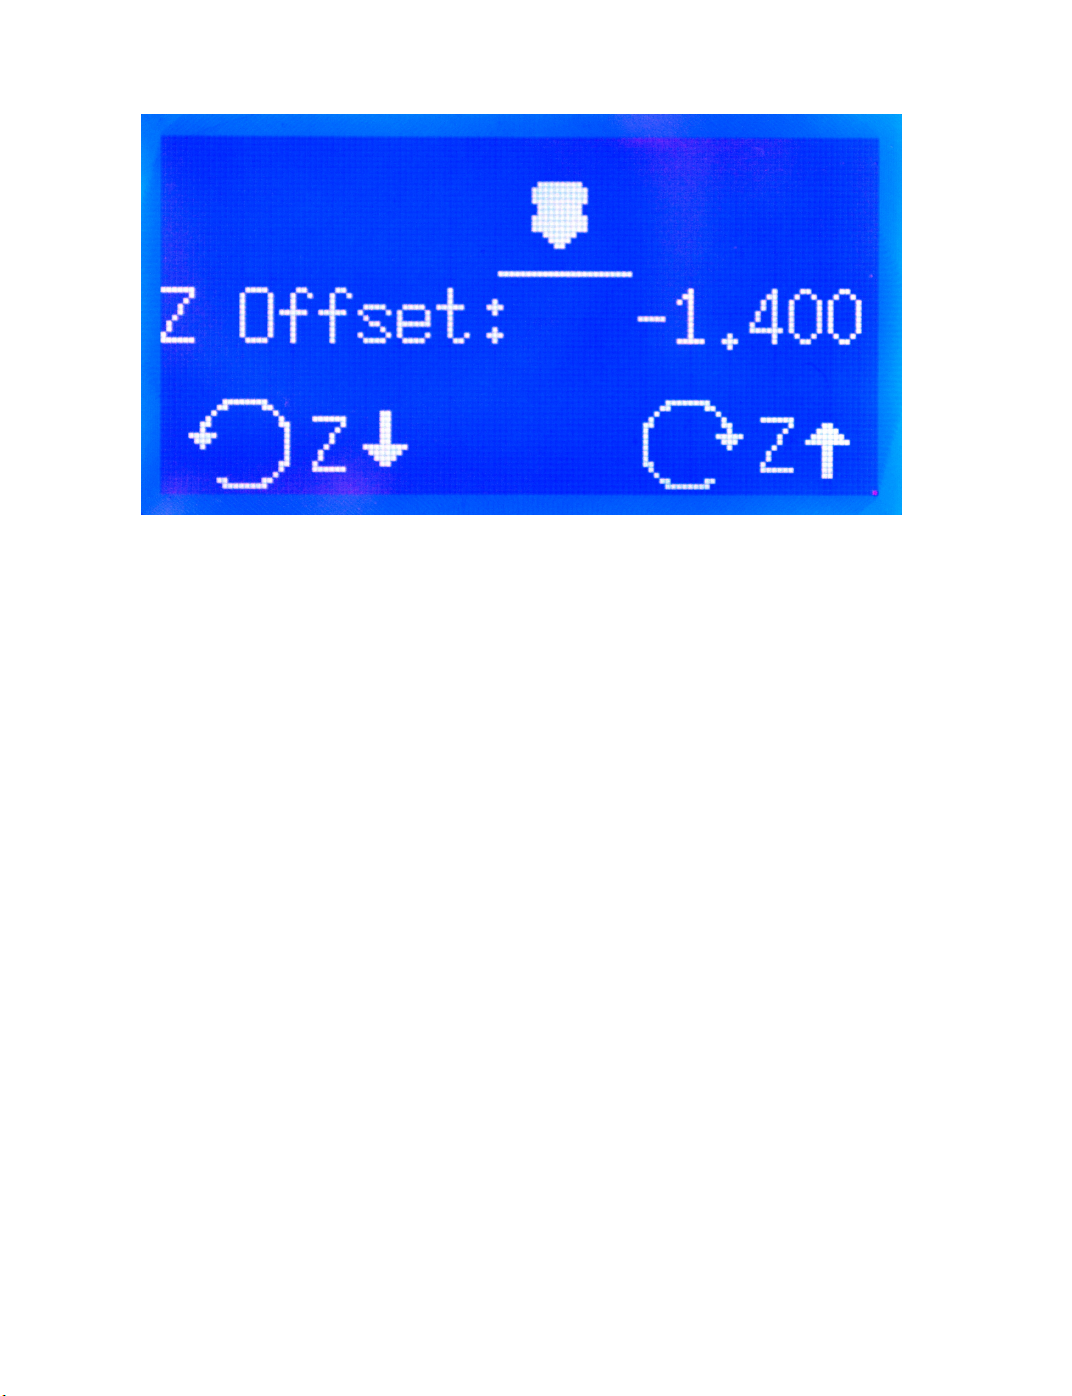
Z Offset
Your LulzBot TAZ 3D printer has the ability to change the rst layer height
(Z oset) directly through the GLCD, even while printing the rst layer.
Using the GLCD, navigate to Configuration -> Advanced Settings ->
Z Offset. While in this screen you can rotate the GLCD knob counterclockwise to bring your nozzle closer to the print surface, and rotate it
clockwise to bring it farther away from the bed. Push in the GLCD knob
to save your settings.
61
PROOF
Page 64
Printing with the Graphic LCD
Figure 3.3: Z Oset Screen
Acceleration
Acceleration is the derivative of speed, and determines how quickly your
print head and bed will reach dened speeds. We have this set to 500mm/s
2
to help prevent resonance and shadowing. This can be increased for sharper
corners and faster turns, however it can lead backlash issues.
Jerk Settings
Jerk is the derivative of accleration and will determine the maximum speed
change allowed at any given time. VXY- Jerk will control jerk setting for
your X and Y-axis. VZ - Jerk will control the jerk setting for your Z-axis.
VE - Jerk will control the jerk settings for your extruder.
Vmax
The Vmax settings will determine the maximum speed that your printer
can move on any specic motor(s). We recommend leaving these settings
as is. Increasing these speeds too much can lead to skipped steps and/or
binding. There will be an individual section for X, Y, Z, and Extruder
motors.
62
PROOF
Page 65
3.6. ADVANCED SETTINGS
Vmin
This sets the minimum overall speeds. We have this set to 0 by default to
allow greater control through your preferred slicing program.
VTrav Min
This will set the minimum travel speed when the tool head is not extruding.
We have this set to 0 by default to allow greater control through your
preferred slicing program.
Amax
The Amax settings will allow you to dene a maximum acceleration limit
for each motor. Increasing these may reduce print time, but can result in
in shadowing and resonance issues.
A-Retract
This sets the maximum acceleration for retraction moves of the extruder.
Going too high can lead to stripping, and going too low can lead to dripping.
We have this set to 3000mm/s2by default.
Steps/mm
Your LulzBot TAZ 3D printer is factory calibrated on all axis for accurate
movement. These settings control that movement, and if adjusted your
objects will not come out at the proper dimensions. We only recommend
adjusting your Esteps/mm as this can be ne tuned for individual tool
heads and laments.
63
PROOF
Page 66
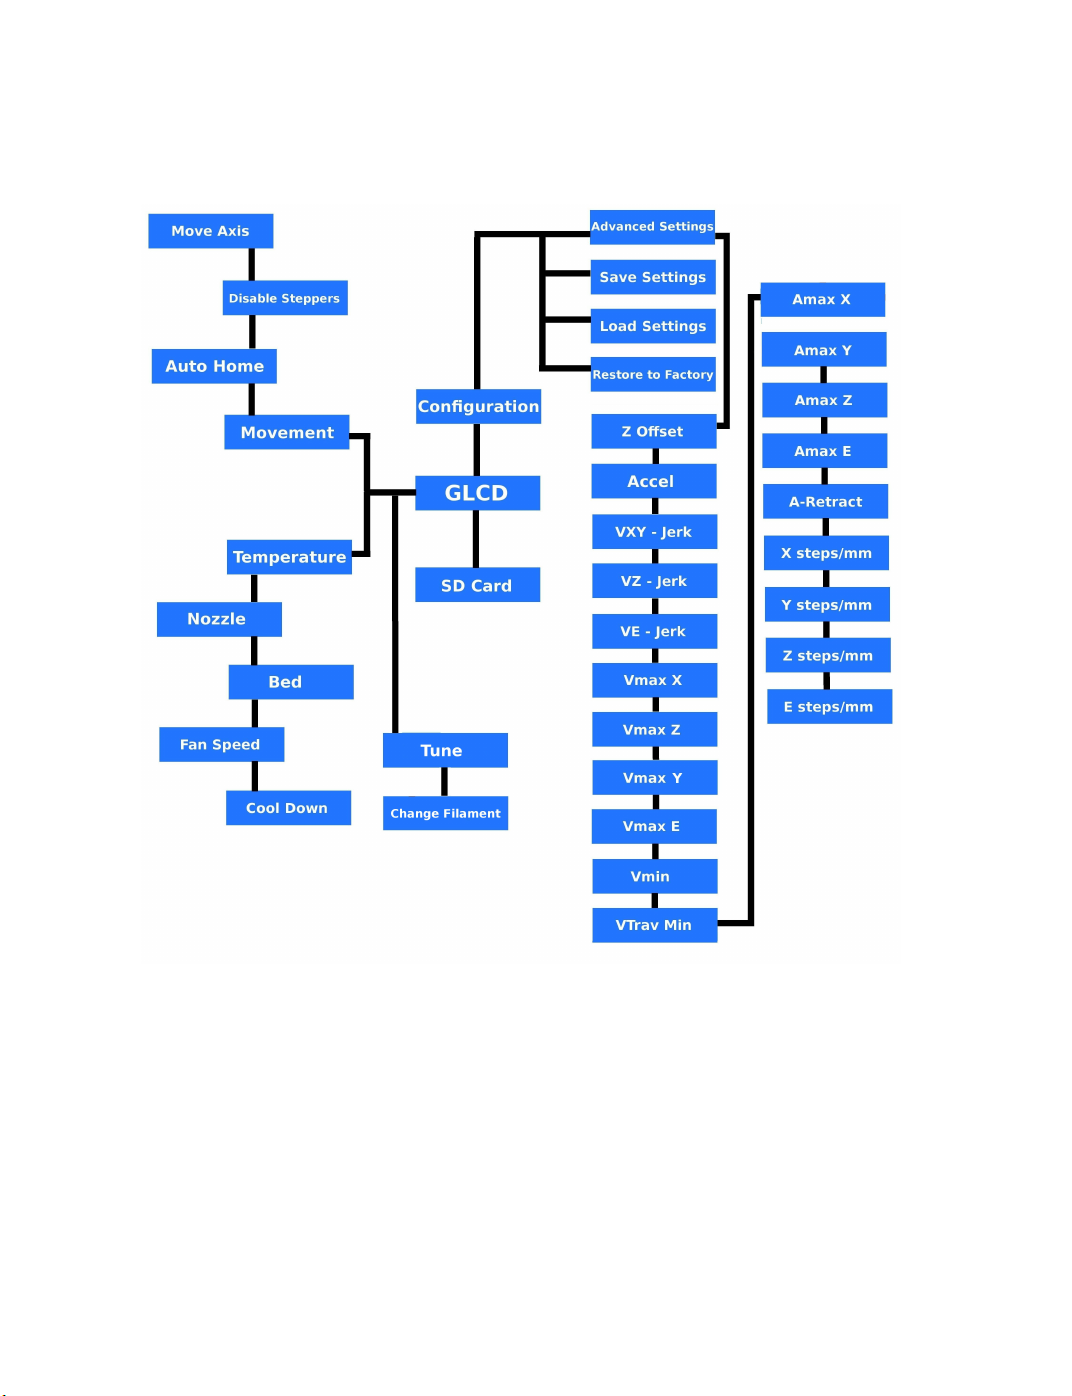
Printing with the Graphic LCD
Graphical LCD Controller Menu Map
Figure 3.4: GLCD Map
64
PROOF
Page 67
Maintaining Your 3D Printer
PROOF
Page 68
Maintaining Your 3D Printer
4.1 Overview
Little maintenance is required keep your LulzBot®TAZ 3D printer running.
Depending on your rate of use you will want to perform a quick check of
your printer every 2 to 4 weeks. The following maintenance guidelines will
keep your printer printing quality parts.
4.2 Smooth Rods
Wipe the smooth steel rods with a clean cloth or paper towel. The linear
bushings leave a solid lubricant that builds up over time. Hearing squeaking
noises while the printer is printing is likely a sign that the smooth rods need
to be cleaned. NOTE: Never apply any lubricant or cleaning agent to the
smooth rods; the bushings are self-lubricating.
4.3 Lead Screw Drive Rods
Periodically, you may want to wipe down the threaded rods with a
lithium-based grease. Never use any petroleum based grease, which may
compromise the plastic parts. We recommend Lucas white lithium grease
NLGI #2. Apply the lithium grease both above and below the X ends on
the threaded rods and wipe down the threaded rods. Use your preferred
printer host software or the Graphical LCD controller to drive the Z-axis
up and down to help further distribute the lubricant. Wipe o any excess
with a clean cloth.
4.4 PEI Print Surface
After repeated use, the PEI print surface will begin to need cleaning.
To clean the PEI print surface, wipe clean with watered-down Isopropyl
Alcohol 10:1 IPA to water ratio and a clean cloth. If you encounter
prints lifting from the PEI surface, use ne grit sandpaper, typically 20002500 grit to clean the PEI print surface. We do not recommend printing
on bare glass, as it can lead to glass bed damage or failure. Never
use acetone to clean the PEI print surface as doing so can damage the
lm. You can nd our maintenance and trouble shooting guides here:
66
PROOF
Page 69
4.5. HOBBED BOLT
https://www.lulzbot.com/learn/tutorials
4.5 Hobbed Bolt
Filament is pulled through the extruder by a hobbed (or toothed) bolt.
After repeated use, the teeth of the hobbed bolt can become lled with
plastic. Using the brush or pick from the printer kit, clean out the hobbed
bolt teeth. If an extruder jam ever occurs, remove the plastic lament from
the extruder and clean out the hobbed bolt.
4.6 Belts
Over long periods or after extensive relocating of the printer you may need
to re-tighten the belts on your 3D printer. For the X-axis, using the 2.5mm
hex driver, loosen one of the belt clamps. The belts clamps are located on
the X-axis carriage. To loosen the belt clamp, loosen the M3 screws on the
clamp. Using the needle nose pliers, pull the belt tight. While holding the
belt tight, tighten down the M3 screw. The Y-axis belt can be tightened
using the same steps as the X-axis using the belt clamps found on the
bottom of the Y-axis plate. Make sure not to over tighten the belts as this
can cause unneeded stress on the printer.
4.7 Hot End
The hot end should be kept clean of extruded plastic by removing melted
plastic strands with tweezers. If melted plastic builds up on the hot end
nozzle you can clean it by raising the head o the build plate, and heating
to extrusion temperature. Using a thick leather glove and a blue shop towel,
carefully wipe o the outside of the hot end. Never use a metal wire brush
on your hot end while powered as it can potentially short the control board.
4.8 Nozzle Wiping Pad
Over time the nozzle wiping pad will become lled with plastic residue.
The pad can be ipped over once and will need to be replaced when
67
PROOF
Page 70
Maintaining Your 3D Printer
full. Replacement nozzle wiping pads are available in our online store at
http://LulzBot.com. Do not attempt to use a plastic or polymer based
wiping pad as it can melt, rather than clean the nozzle. A metal wiping
pad should never be used, as it can cause electrical shorts. If the nozzle is
not clean during the bed-level calibration process the print surface or tool
head can be damaged.
4.9 Bed Leveling Washers
Keep the washers mounted on each corner of the print surface clean and
dust free by wiping them periodically with Isopropyl Alcohol (IPA), or a
clean dry cloth. If the bed leveling washers are not clean during the bed
calibration process the print surface or tool head may be damaged. Never
attempt to clean the bed leveling washers during the probing sequence as
it may lead to personal injury.
4.10 Cooling Fans
Every 2-4 weeks carefully clean your hot end cooling fans by rst unplugging
the tool head from the extruder harness. Gently blow any dust away with
short bursts with a can of compressed air.
4.11 Electronics
The electronics case holding the RAMBo board may need dust blown out
occasionally. Power down the printer and use short bursts of compressed
air to blow out any dust.
68
PROOF
Page 71
Advanced Usage
PROOF
Page 72
Advanced Usage
5.1 Intro
After you become familiar with printing using the default settings, a few
advanced techniques may help in getting better and more consistent prints
from the LulzBot®TAZ 3D printer. Some of these instructions are items
and materials not included with the TAZ. With any of these additional
items or materials, follow safety and usage guidelines as instructed by the
manufacturer.
5.2 Changing nozzles
Nozzle related issues will not be covered under warranty after nozzle
changes.
Your hot end is equipped with a 0.50mm nozzle. This nozzle diameter
will print faster than a 0.35mm nozzle. Purchase a tool head from
LulzBot.com with an alternate nozzle diameter for quick, easy, and simple
changes.
Due to the specic torque of 30 inch pounds required to tighten the
nozzle when removed, removing the nozzle is not recommended. Failure to
properly tighten the nozzle to the specic recommended torque may lead
to leaks or damage if over-tightened.
5.3 Bed Adhesion
You may nd that during printing, printed parts lift o the print surface on
the corners. If you are seeing this turning on Brim in Cura will help increase
the surface area of the print, improving part adhesion. If the corners of the
part still lift, clean the PEI surface with IPA/ Isopropyl Alcohol and sand
the surface with ne grit (2000-3000) sandpaper.
ABS/Acetone Glue
Acetone is not included or required with the LulzBot TAZ 3D printer.
Acetone and ABS solution is NOT recommended anymore, as the PEI
print surface works well without it.
70
PROOF
Page 73
5.4. USING 1.75MM FILAMENT
Glue stick/PVA Glue solution
While almost all 3D printing laments will adhere well to the PEI print
surface, Nylon, and Amphora™-based print adhesion can be improved with
the application of an unscented PVA glue solution/glue stick. Flexible
laments such as NinjaFlex®and SemiFlex™can adhere too well and can
be released easier from the PEI print surface with an application of an
unscented PVA glue solution/glue stick to the print surface prior to starting
the printing process.
5.4 Using 1.75mm filament
Your LulzBot TAZ 3D printer is set up to use 3mm plastic lament by
default and may be capable of printing 1.75mm lament with no hardware
modication. While many of our advanced users are able to do so, your
results may vary. More information can be found in our User Forums at:
https://forum.lulzbot.com/viewtopic.php?f=16&t=1923
71
PROOF
Page 74
PROOF
Page 75
Hardware and Software Source Code
PROOF
Page 76
Hardware and Software Source Code
The LulzBot®TAZ 3D printer is a Free Software and Open
Source Hardware design. All of the source les are available at
http://download.lulzbot.com/TAZ including:
• The latest version of this document, with LATEX source code.
• 3D models and print les for all of the printed parts in .stl, .gcode,
and other original source les.
• 3D calibration objects and random novelties.
• Production le for calculating large print runs.
• Design les for all electronics and machined parts.
– LulzBot®Hexagon Hot End
– RAMBo electronics
– Various spec sheets
• Bill of materials including every part needed to build the printer.
– TAZ
– LulzBot Hexagon Hot End
• Drawings of components.
– Aluminum extrusions
– LulzBot Hexagon Hot End
– Bed plate
• Software binaries and source code for GNU/Linux and others. Also
includes known good conguration les.
– Cura
– Marlin
74
PROOF
Page 77
3D Printer Support
PROOF
Page 78
3D Printer Support
7.1 LulzBot
For common technical support questions for your LulzBot®TAZ 3D printer
please visit LulzBot.com/support. Also, visit Forum.LulzBot.com for
support and tips from the LulzBot 3D printer community. If you have
further questions, e-mail our support team at [email protected].
Please completely read this manual before contacting for support questions
or help. The latest version of this information guide is also available
at http://download.lulzbot.com. You can also nd more information
including images, videos, and updated versions of this manual in the
Support section of LulzBot.com.
7.2 Support
Email: [email protected]
Phone: +1-970-377-1111 x610
7.3 Regional Phone Numbers
Regional phone numbers are available at LulzBot.com/contact-us.
7.4 Community
Community Support and Resources
• LulzBot 3D printer forum: Forum.LulzBot.com
• LulzBot Online Community: LulzBot.com/community
76
PROOF
Page 79
Warranty Information
PROOF
Page 80
Warranty Information
8.1 Warranty
Warranty information for your LulzBot®TAZ 3D printer can be found at
https://www.lulzbot.com/support/warranty
Extended Warranty
Optional extended warranty terms are available for purchase at
https://www.lulzbot.com/store/parts/lulzbot-taz-extended-warranty.
8.2 Modification Warning
WARNING: At Aleph Objects, Inc®we respect your freedom to modify your
LulzBot desktop 3D printer. However, any modifications or attempted
repairs that cause damage are not covered under the Warranty.
Questions? Contact Technical Support by emailing [email protected]
or by calling +1-970-377-1111.
78
PROOF
Page 81
Contact Information
PROOF
Page 82
Contact Information
9.1 Support
Email: [email protected]
Phone: +1-970-377-1111 x610
9.2 Sales
Email: [email protected]
Phone: +1-970-377-1111 x600
9.3 Regional Phone Numbers
Regional phone numbers are available at LulzBot.com/contact-us.
9.4 Websites
Aleph Objects, Inc., the makers of the LulzBot®brand of 3D Printers:
www.AlephObjects.com
LulzBot 3D Printers and parts:
www.LulzBot.com
Forum.LulzBot.com
80
PROOF
Page 83
Index
Symbols
1.75mm lament, 71
A
ABL, 27
ABS, 70
acetone, 67, 70
Adhesion Type, 35
Advanced Options, 36
advanced techniques, 70
Airgap, 47
aluminum extrusions, 74
Australia, x
auto-leveling, 68
Automatic Bed Leveling, 27
B
Base Line Width, 47
Base Thickness, 47
Basic Options, 32
bed adhesion, 70, 71
bed plate, 74
Bed Temperature, 34
belts, 67
bill of materials, 74
Black Magic, 46
Blender, 14
blowers, 68
BotQueue, 14
bottle, 70
Bottom Layer Speed, 38
Bottom Thickness, 33
Brim, 20, 35, 46
brim, 70
burns, viii
bushings, 66
C
CAD, 13
Calibrating Extruders, 50
calibration, 74
Combine Type-A, 48
Combine Type-B, 48
Combing, 43
community support, 76
Cooling, 44
Cura, 18, 74
Custom GCODE, 41
Cut O Object, 37
D
damage, 78
download, 12, 74
drive rods, 66
driver, 12
Dual Extrusion, 49
Dual Extrusion Overlap, 38
81
PROOF
Page 84
INDEX
E
eeprom settings, 60
electronics, viii, 68, 74
Enabling Cooling Fan, 39
End GCODE, 41
Expert Settings, 42
extended warranty, 78
Extensive Stitching, 48
Extra Margin, 47
extruder, viii
extruder jam, 67
F
failed repair, 78
fan, 68
Fan Settings, 44
FCC, ix
lament, 20
Filament Diameter, 36
Fill Amount, 45
Fill Density, 33
First Dual Print, 51, 52
First Print, 27
Fix Horrible, 48
Flow Rate, 36
forums, 76
FreeCAD, 13
Freenode, 76
Full Settings, 31
G
g-code, 12
GCODE, 12
gcode, 74
Ghost View, 25
glass, 66, 67
GLCD, 27
Glue stick, 29, 71
gluestick, 71
GNU/Linux, 12–14
Graphical LCD controller, 27
grease, 66
H
hardware, 74
hazards, viii
heater block, viii
Hexagon, 74
hexagon, 74
High Detail, 19
high resolution, 70
High Speed, 20
hobbed bolt, 67
Host, 14
hot end, 67, 70
I
ICES, x
Inll Speed, 38
Initial Layer, 37
Initial Layer Width, 37
Inner Shell Speed, 39
Installation, 18
Interface Line Width, 47
Interface Thickness, 47
IPA, 70
IRC, 76
Isopropyl Alcohol, 66
Isopropyl alcohol, 70
L
latex, 74
Layer Height, 32
Layers View, 26
lead screw, 66
leveling, 68
Line Count, 43
82
PROOF
Page 85
INDEX
Line Spacing, 47
Load Model, 20
lubricant, 66
M
maintenance, 66
Marlin, 74
Material Selection, 20
MatterControl, 15
Minimal Layer Time, 39
Minimal Length, 44
Minimum Travel, 43
modication, 78
N
New Zealand, x
Ninjaex, 70
Normal View, 23
novelties, 74
nozzle, 67, 70
nozzle cooling fan, 68
Nozzle Size, 36
nozzle wipe, 67
Nylon, 70, 71
O
OctoPrint, 14
Open Faces, 48
OpenSCAD, 13
operating system, 12
Orientation, 21
OS X, 12–15
Outer Shell Speed, 39
Overhang Angle, 45
Overhang View, 24
P
Pause, 29
Pause at Z Height, 40
PEI, 70
PEI surface, 66
Plugins, 39
power supply, viii
print cooling fan, 68
Print Speed, 33
printed parts, 74
Printer Host, 12
printing, 28
Printing from SD, 27
Printing from USB, 28
Printing Temperature, 34
probe, 68
probing, 68
Probing Temperature, 41
PVA, 71
Q
Quick Print Prole, 19
Quick Print Settings, 19
R
Raft, 35, 46
RAMBo, 68, 74
Removing a Print, 30
RepRap, 76
Resolution, 19
Retraction, 33, 42
Retraction Distance, 36
Retraction Speed, 36
Rotating Object, 21
S
SD, 27
SD card, 27
Second Extruder Oset, 50
Shapesmith, 14
Shell Thickness, 33
Skirt, 43
83
PROOF
Page 86
INDEX
Slicers, 12
Slicing, 12
smooth rods, 66
software, 12–14, 74
Source Code, 74
Source Files, 15
Spiralize, 46
Standard Quality, 20
Start Distance, 44
Start GCODE, 41
STL, 13, 14, 20, 74
Support, 45
Support Material, 20, 45
Support Settings, 45
Support Type, 34
Surface Layers, 48
T
technical support, 76
temperature, viii
Temperatures, 29
terms and conditions, 78
threaded extension, 70
threaded rods, 66
Top Thickness, 33
Travel Speed, 38
Tweak at Z, 40
U
Updating Firmware, 49
V
View Options, 23
W
warnings, viii
warping, 70
warranty, 78
Windows, 12–15
wiping pad, 67
Wiping Temperature, 41
wires, viii
X
Xray, 25
Z
Z hop, 43
Z Oset, 61
84
PROOF
Page 87
Glossary
.GCODE The le extension for G-Code les
Cura Cura LulzBot Edition is a cross-platform software package that
combines a slicing engine with a printer host interface.
3D Printer Also referred to as additive manufacturing, is the process of
fabricating objects from 3D model data, through the deposition of a
material in accumulative layers.
ABS Acrylonitrile butadiene styrene thermoplastic. Usually extrudes at
230°C with the Budaschnozzle and 240°C - 250°C with the LulzBot
Hexagon Hot End.
Acetone A colorless, volatile, ammable liquid ketone, (CH3)2CO, used as
a solvent for ABS.
CAD Computer Aided Design
FFF Fused Filament Fabrication– the process of laying down successive
layers of extruded lament to create a 3 dimensional object. As each layer
of molten plastic is extruded into place, it fuses with the previous layer.
Filament Plastic material in a “string” like form, as it is fed to the printer.
Free Software Free Software (or Free/Libre Software) can be thought of as
“free as in free speech, not just free as in free beer”, although most Free
Software is available for no cost. Free Software can be copied, modied and
is freely available for download.
GCODE The common name for the most widely used CNC programming
language.
HDPE High-density polyethylene.
Heater block Machined from aluminum, the heater block generates heat
with a heater resistor and uses a thermistor to measure the temperature.
85
PROOF
Page 88
GLOSSARY
Heater resistor A special type of resistor that is used to apply heat in a
small area.
HIPS High-impact polystyrene. Usually extrudes at 230°C with the
Budaschnozzle and 230°C with the LulzBot Hexagon Hot End
Hot end The hot end is the whole part where the plastic melts, including
the nozzle, heater block, thermistor, and heat sink. The LulzBot Hexagon
Hot End comes standard on the TAZ 5.
Layer height The thickness of each individual deposited layer of the threedimensional model when cut with a slicing program.
Laywoo-D3 Wooden lament similar to PLA. Forty percent of its content
consists of recycled wood. Usually prints at 180°C to 210°C. Color can
be changed by varying the extrusion temperature.
Libre Innovation Aleph Objects uses Free/Libre Software to build and
improve Open Source Hardware so that everything we create is free to
be viewed, copied, and/or modied by anyone.
Nozzle The metal tip at the bottom of the hot end. It has a small hole
where the plastic lament comes out of the printer.
Open Source Hardware Open source hardware is hardware whose design
is made publicly available so that anyone can study, modify, distribute,
make, and sell the design or hardware based on that design. The
hardware source, the design from which it is made, is available in the
preferred format for making modications to it. For more information
visit http://www.oshwa.org/definition/.
PLA Polylactic acid is a corn-based biodegradable polymer. Usually
extrudes at 185°C with the Budaschnozzle and 205°C with the LulzBot
Hexagon Hot End.
Polycarbonate A strong and impact-resistant thermoplastic. Usually ex-
trudes at 300°C.
PTFE Polytetrauoroethylene is a synthetic uoropolymer used in the Budaschnozzle for it’s low coecient of friction. This limits the Budaschnozzle
top extrusion temperature to 250°C. The LulzBot TAZ 5 and TAZ 6 does
not use a hot end with a PTFE insert and can reach a 300°C extrusion
temperatuere.
PVA Polyvinyl acetate is the main ingrediant in white glue, wood glue and
the common school glue stick.
86
PROOF
Page 89
GLOSSARY
RAMBo [R]epRap [A)]duino-[M]ega compatible [M]other [Bo]ard. Designed
by Joynnyr of UltiMachine.
Resolution In general terms, the resolution you print at can be determined
by the layer height you use. The LulzBot TAZ can print at a layer height
of 0.05mm to 0.50mm.
Slic3r Slic3r is a cross-platform 3D model slicing engine. It’s used to process
the 3 dimensional model into the GCODE (tool path) needed to physically
generate the print.
Spool Plastic lament coiled and stored on a plastic reel. Preferred over
1.75mm lament due to improved feeding and better mounting options.
Thermistor A special type of resistor that changes resistance based on
temperature. It is used to measure temperature on the nozzle and the
heated bed.
Threaded extension Used to separate the heater block and nozzle from
the PEEK insulator. The plastic lament passes through the threaded
extension into the melting chamber.
87
PROOF
Page 90
PROOF
Page 91
Colophon
Created with 100% Free/Libre Software
GNU/Linux
LATEX Memoir
PROOF
Page 92
PROOF
,!7IA9I9-dhieic!
Page 93
PROOF
 Loading...