

Page 1
TAZ 5 User Manual
Aleph Objects, Inc.
Page 2
LulzBot™TAZ 5 User Manual
by Aleph Objects, Inc.
Copyright © 2015 Aleph Objects, Inc.
Permission is granted to copy, distribute and/or modify this document
under the terms of the Creative Commons Attribution 4.0 International
Public License (CC BY-SA 4.0).
Published by Aleph Objects, Inc., 626 W 66th Street, Loveland, Colorado,
80538 USA.
For more information, call +1-970-377-1111 or go to www.LulzBot.com and
www.AlephObjects.com.
ISBN: 978-0-9893784-7-5 5.0-20150910
Page 3
Contents
WARNINGS
Safety Information · · · · · · · · ix
Read Me First! · · · · · · · · · · · · · · · · x
Hazards and Warnings · · · · · · · · · · · · · · x
1 3D Printer Software · · · · · · · 13
1.1 Software Overview · · · · · · · · · · · · · 14
1.2 Software Types · · · · · · · · · · · · · · 14
1.3 Installing Drivers · · · · · · · · · · · · · · 15
1.4 Cura · · · · · · · · · · · · · · · · · · 15
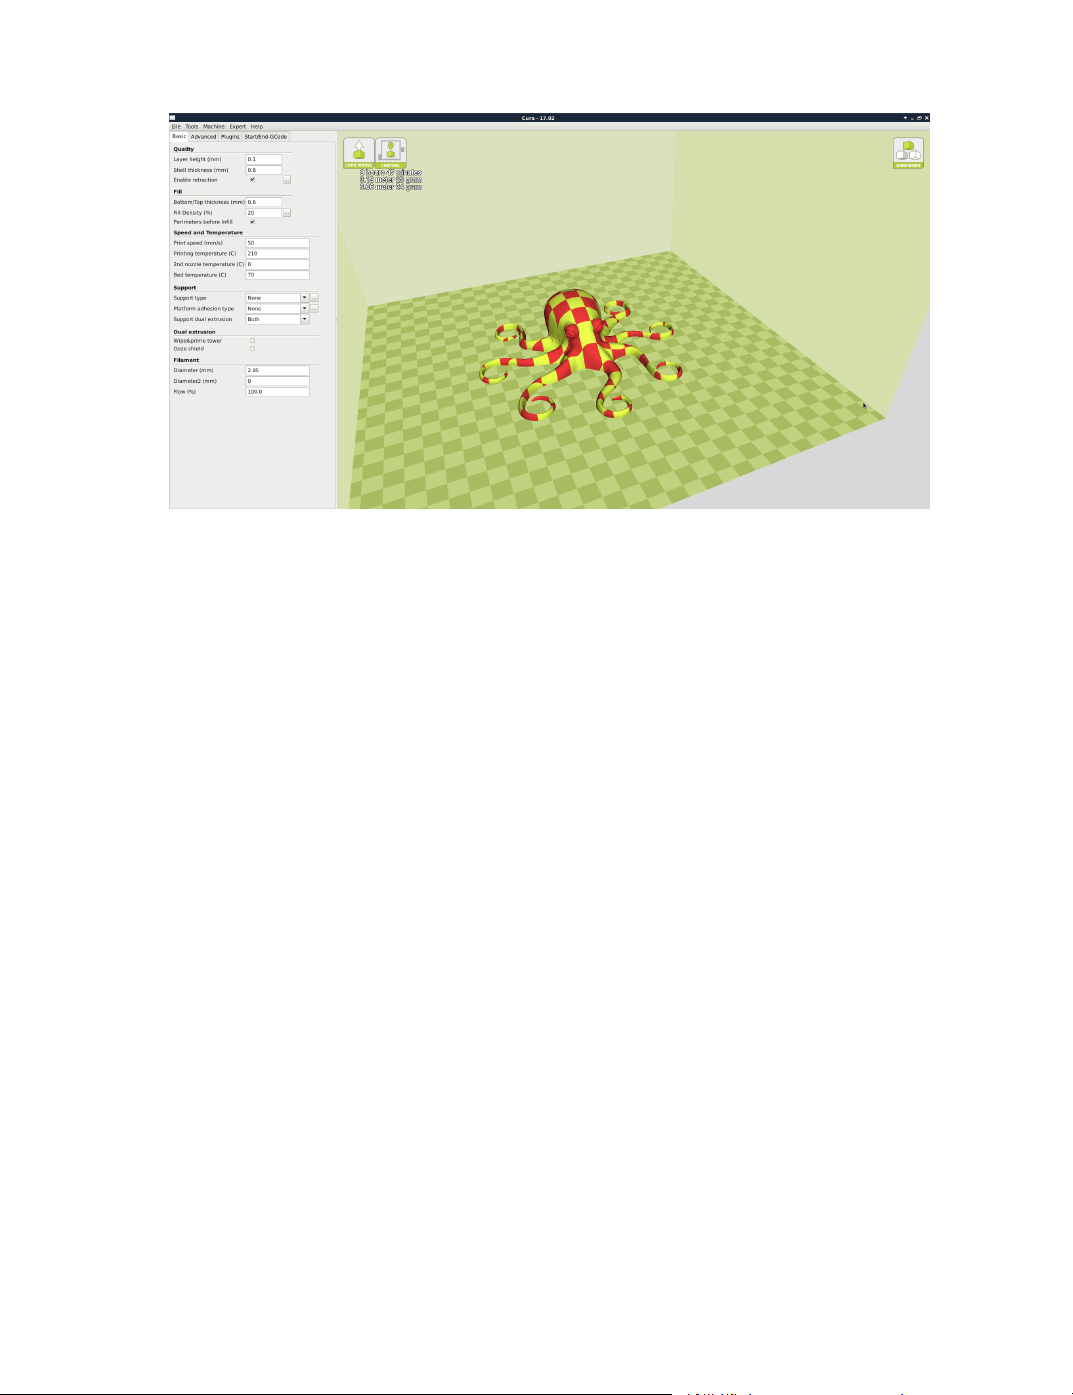
1.5 Quick Print Settings · · · · · · · · · · · · · 17
1.6 View Options · · · · · · · · · · · · · · · 21
1.7 Starting Your First Print · · · · · · · · · · · 25
1.8 Removing Your First Print · · · · · · · · · · 27
1.9 Full Settings · · · · · · · · · · · · · · · 28
1.10 Basic Tab Options · · · · · · · · · · · · · 29
1.11 Advanced Tab Options · · · · · · · · · · · · 33
1.12 Plugins · · · · · · · · · · · · · · · · · 36
1.13 Start and End Gcode Settings · · · · · · · · · 38
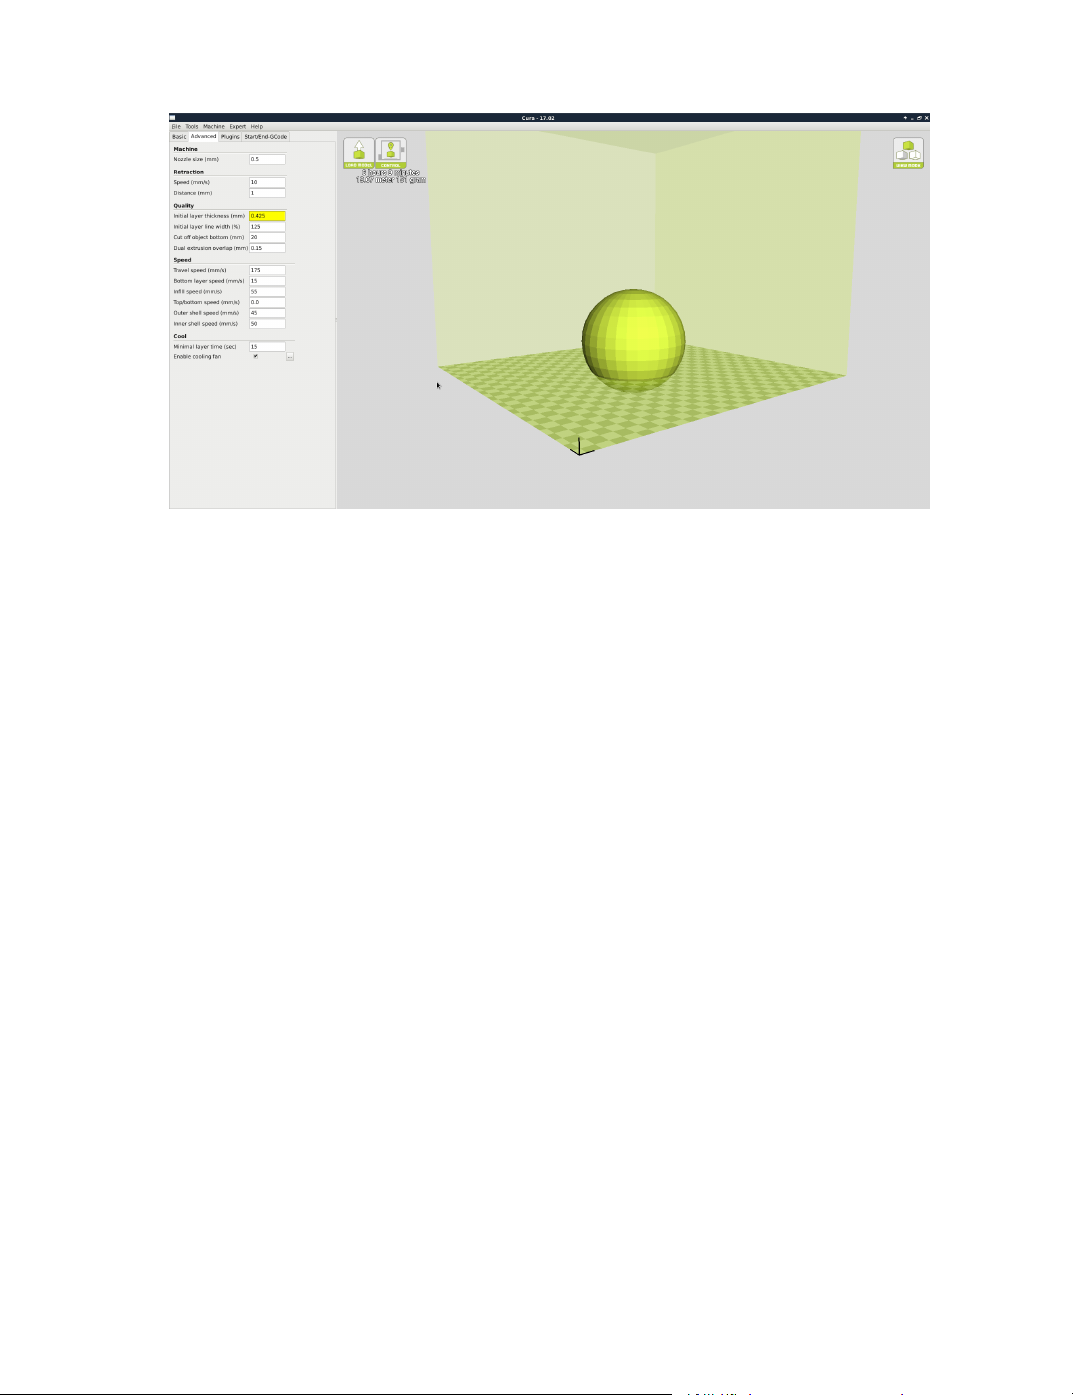
1.14 Expert Settings · · · · · · · · · · · · · · 38
1.15 Retraction · · · · · · · · · · · · · · · · 39
1.16 Skirt · · · · · · · · · · · · · · · · · · 39
1.17 Cool · · · · · · · · · · · · · · · · · · 40
1.18 Support · · · · · · · · · · · · · · · · · 41
1.19 Black Magic · · · · · · · · · · · · · · · 42
1.20 Brim · · · · · · · · · · · · · · · · · · 42
1.21 Raft · · · · · · · · · · · · · · · · · · 43
1.22 Fix Horrible · · · · · · · · · · · · · · · 44
1.23 Dual Extrusion · · · · · · · · · · · · · · 45
iii
Page 4
CONTENTS
1.24 Printrun · · · · · · · · · · · · · · · · · 50
1.25 Using Printrun · · · · · · · · · · · · · · 52
1.26 CAD and 3D Modeling Software · · · · · · · · 56
1.27 Alternative Printer Host Software · · · · · · · · 57
2 Slic3r · · · · · · · · · · 59
2.1 Introduction · · · · · · · · · · · · · · · 60
2.2 Getting Slic3r · · · · · · · · · · · · · · · 61
2.3 First Print · · · · · · · · · · · · · · · · 62
2.4 Simple Mode · · · · · · · · · · · · · · · 79
2.5 Expert Mode · · · · · · · · · · · · · · · 88
2.6 Conguration Organization · · · · · · · · · · 117
2.7 Repairing Models · · · · · · · · · · · · · · 119
2.8 Advanced Topics · · · · · · · · · · · · · · 120
2.9 Troubleshooting · · · · · · · · · · · · · · 133
2.10 Slic3r Support · · · · · · · · · · · · · · · 138
3 Printing with the Graphic LCD · · · · · 141
3.1 GLCD Controller, Cura or Printrun Host? · · · · · 142
3.2 Multiple Connections · · · · · · · · · · · · 142
3.3 Putting Print Files on the SD Card · · · · · · · 143
3.4 Printing With the Graphic LCD · · · · · · · · · 144
4 Maintaining Your 3D Printer · · · · · · 147
4.1 Overview · · · · · · · · · · · · · · · · 148
4.2 Smooth Rods · · · · · · · · · · · · · · · 148
4.3 Lead Screw Drive Rods · · · · · · · · · · · · 148
4.4 PEI Surface · · · · · · · · · · · · · · · 148
4.5 Hobbed Bolt · · · · · · · · · · · · · · · 149
4.6 Belts · · · · · · · · · · · · · · · · · · 149
4.7 Hot End · · · · · · · · · · · · · · · · · 149
4.8 Electronics · · · · · · · · · · · · · · · · 149
5 Advanced Usage · · · · · · · · 151
5.1 Intro · · · · · · · · · · · · · · · · · · 152
5.2 Changing nozzles · · · · · · · · · · · · · · 152
5.3 Bed Adhesion · · · · · · · · · · · · · · · 152
5.4 Using 1.75mm lament · · · · · · · · · · · · 153
6 Hardware and Software Source Code · · · · 155
iv
Page 5
CONTENTS
7 3D Printer Support · · · · · · · 157
7.1 LulzBot · · · · · · · · · · · · · · · · · 158
7.2 Community · · · · · · · · · · · · · · · · 158
8 Warranty Information · · · · · · · 159
8.1 Warranty · · · · · · · · · · · · · · · · 160
9 Contact Information · · · · · · · 161
9.1 Support · · · · · · · · · · · · · · · · · 162
9.2 Sales · · · · · · · · · · · · · · · · · · 162
9.3 Websites · · · · · · · · · · · · · · · · · 162
Index · · · · · · · · · · · 163
Glossary · · · · · · · · · · 169
v
Page 6
List of Figures
1.1 Quick Print Settings · · · · · · · · · · · · · · 17
1.2 Options after selecting model · · · · · · · · · · · 19
1.3 Rotating your Model · · · · · · · · · · · · · · 20
1.4 Scaling your Model · · · · · · · · · · · · · · 21
1.5 View in Normal Mode · · · · · · · · · · · · · 22
1.6 View in Overhang · · · · · · · · · · · · · · · 22
1.7 View in Ghost · · · · · · · · · · · · · · · · 23
1.8 View in Xray · · · · · · · · · · · · · · · · 23
1.9 View in Layers · · · · · · · · · · · · · · · · 24
1.10 Viewing Cumulative Layers · · · · · · · · · · · 24
1.11 Viewing Specic Layers · · · · · · · · · · · · · 25
1.12 Control Screen · · · · · · · · · · · · · · · · 26
1.13 View in Full Settings · · · · · · · · · · · · · · 28
1.14 Dierences in Layer Height · · · · · · · · · · · 29
1.15 Support Types · · · · · · · · · · · · · · · · 32
1.16 Cuto Example · · · · · · · · · · · · · · · 35
1.17 View of Plugins · · · · · · · · · · · · · · · 37
1.18 View Expert Settings · · · · · · · · · · · · · 38
1.19 Before Merge · · · · · · · · · · · · · · · · 48
1.20 After Merge · · · · · · · · · · · · · · · · · 49
1.21 Printrun application for 3D printer control · · · · · · 50
1.22 Printrun · · · · · · · · · · · · · · · · · · 52
1.23 Printrun Functions · · · · · · · · · · · · · · 54
1.24 Movement Controls · · · · · · · · · · · · · · 54
2.1 Conguration Wizard: Welcome Screen · · · · · · · 64
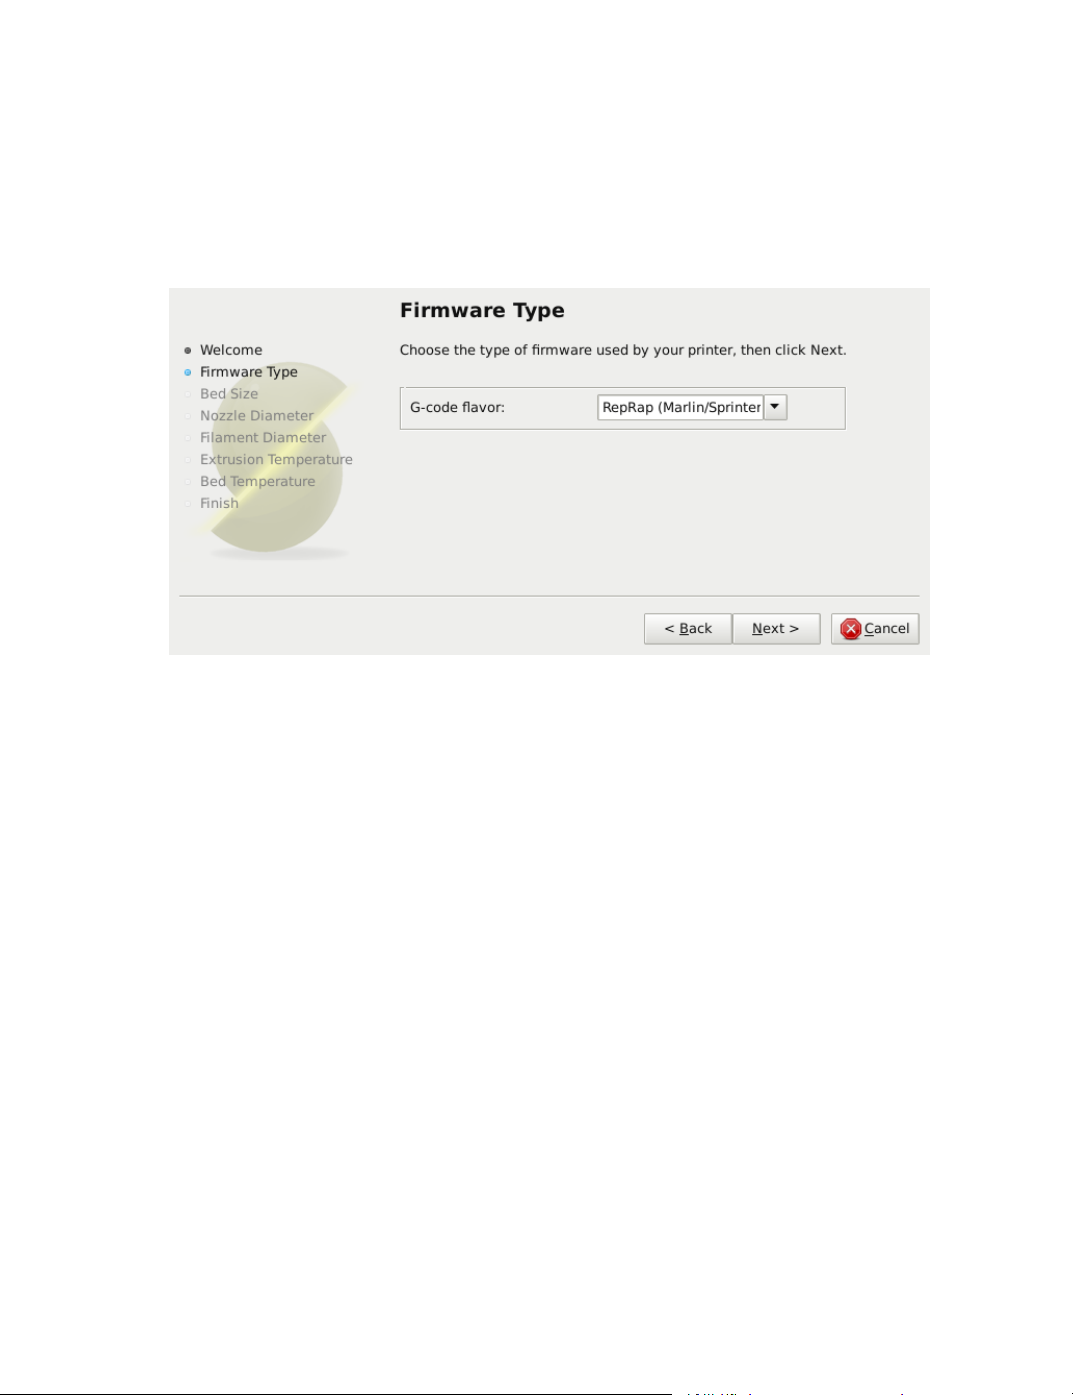
2.2 Conguration Wizard: Firmware Type · · · · · · · · 65
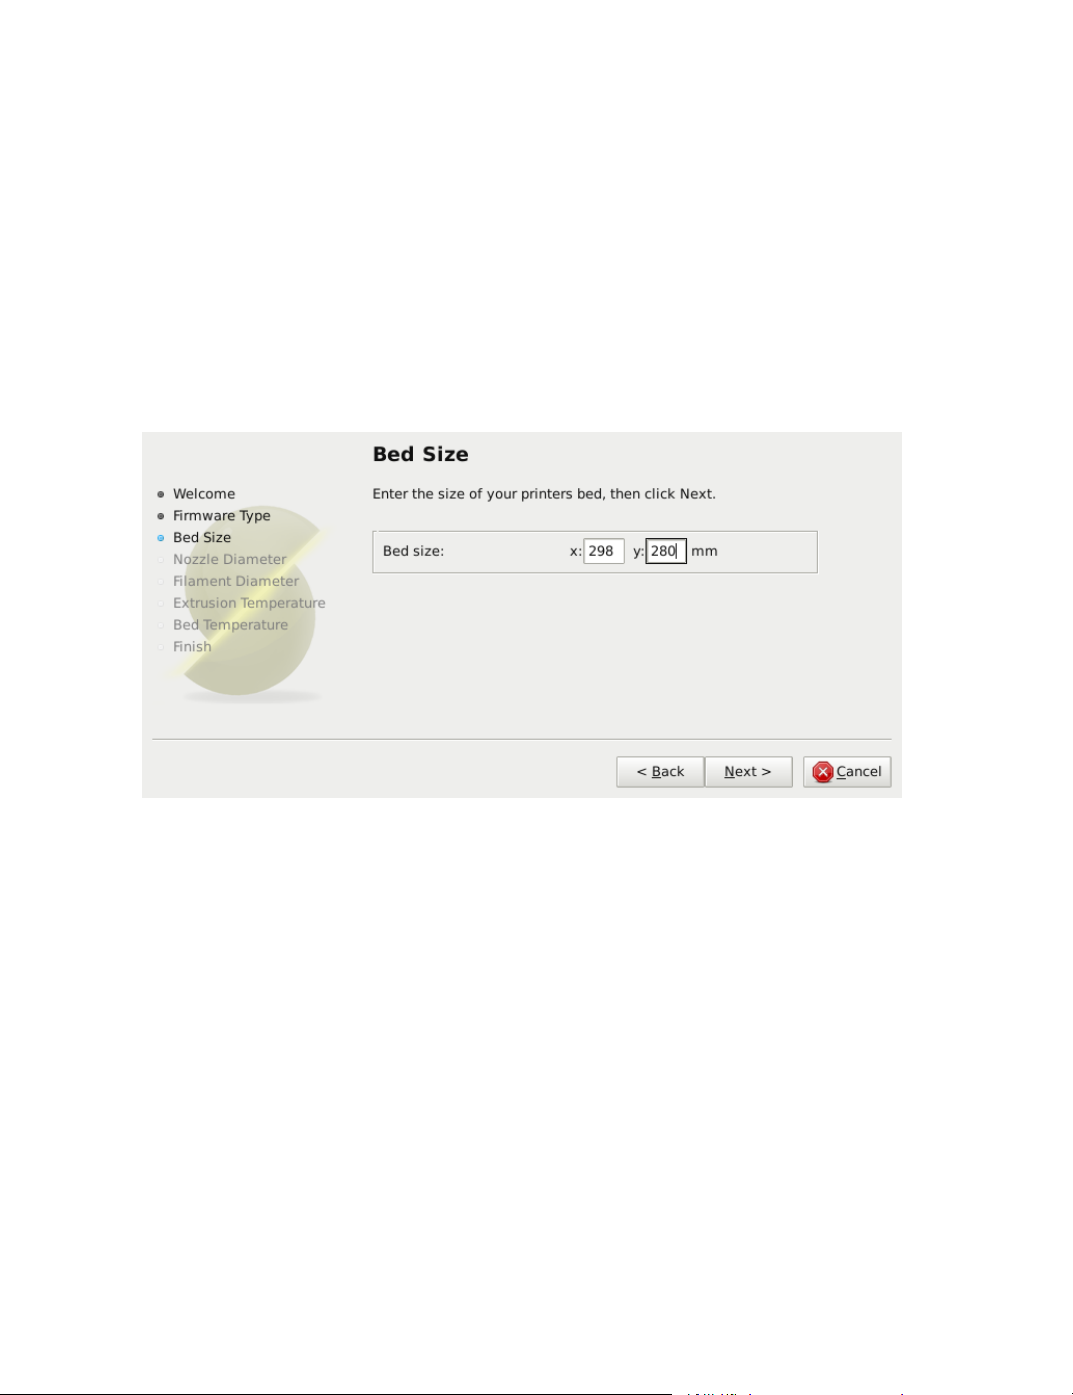
2.3 Conguration Wizard: Bed Size · · · · · · · · · · 66
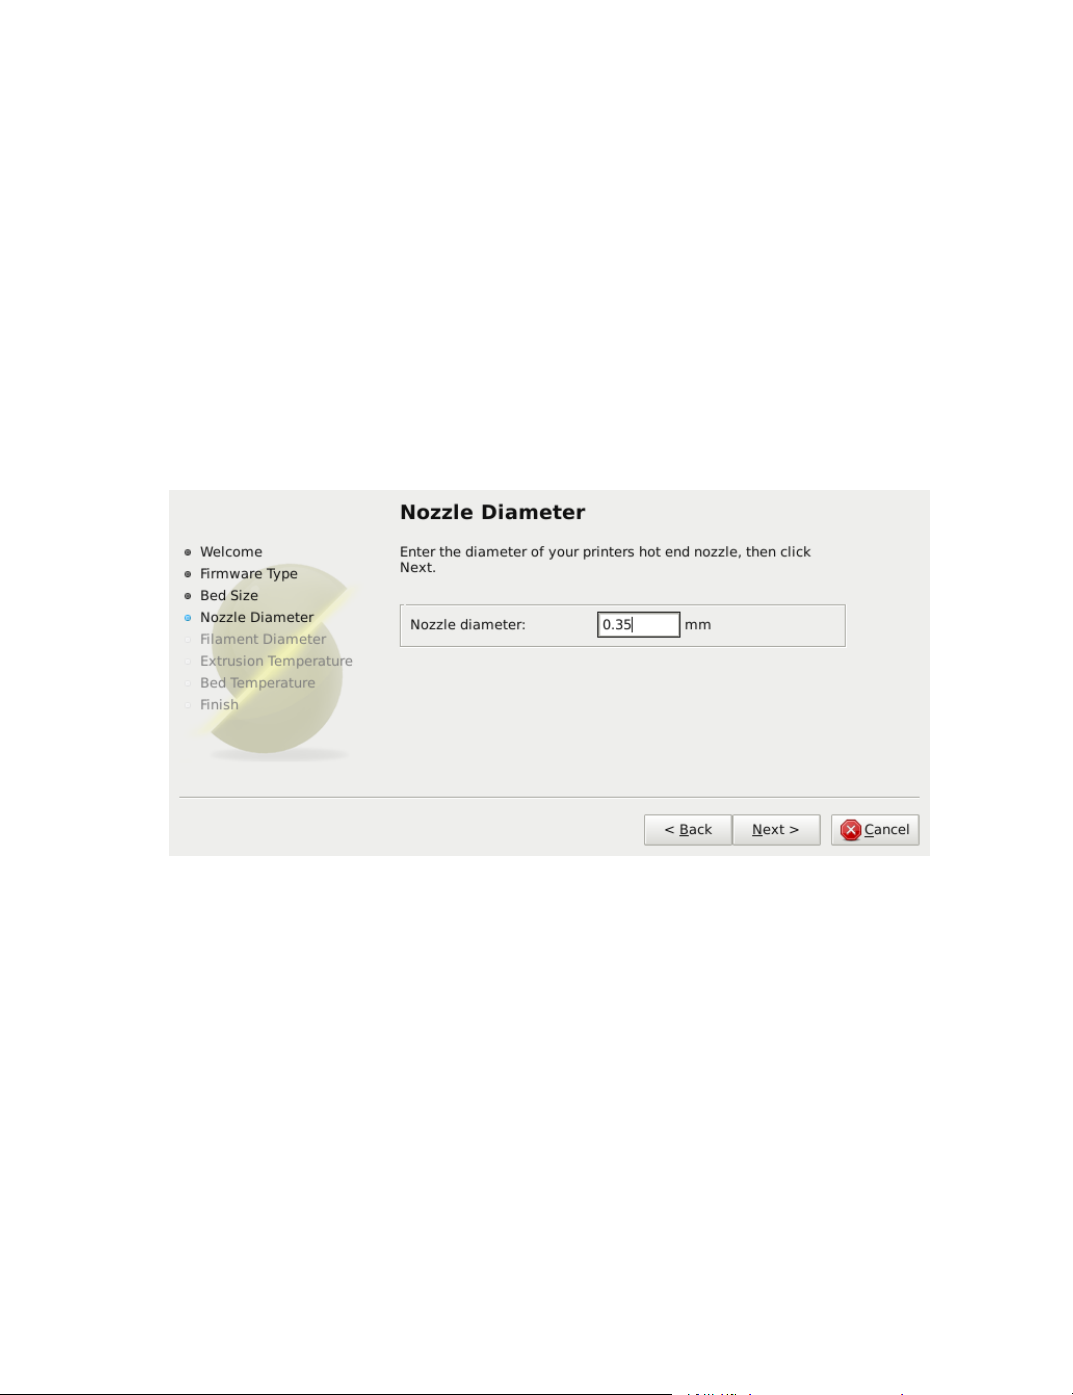
2.4 Conguration Wizard: Nozzle Diameter · · · · · · · 67
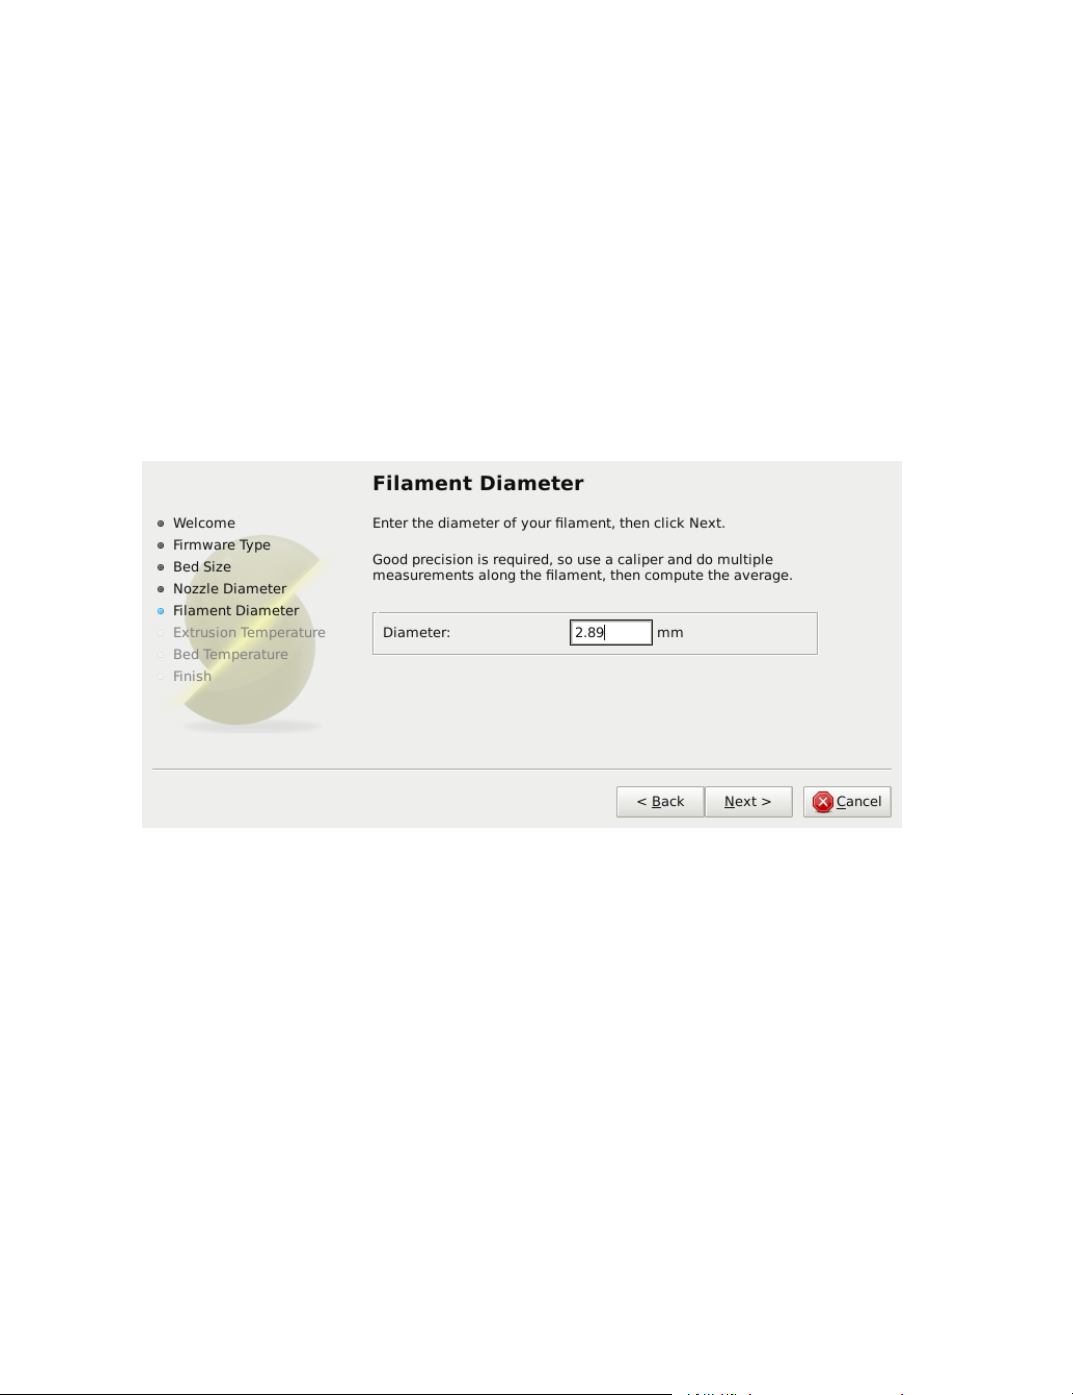
2.5 Conguration Wizard: Filament Diameter · · · · · · 68
2.6 Conguration Wizard: Extrusion Temperature · · · · · 69
2.7 Conguration Wizard: Bed Temperature · · · · · · · 70
2.8 Conguration Wizard: End · · · · · · · · · · · 71
2.9 Shapesmith online CAD tool. · · · · · · · · · · · 75
vi
Page 7
List of Figures
2.10 Plater · · · · · · · · · · · · · · · · · · · 76
2.11 Minimug model. · · · · · · · · · · · · · · · 77
2.12 STL le loaded. · · · · · · · · · · · · · · · 77
2.13 Preferences. · · · · · · · · · · · · · · · · · 79
2.14 Simple Mode: Print Settings. · · · · · · · · · · · 80
2.15 An example of insucient top layers. · · · · · · · · 81
2.16 Creating a vase from a solid model. · · · · · · · · · 82
2.17 An example of an object printed with support material. · · 83
2.18 An example of brim. · · · · · · · · · · · · · · 84
2.19 Simple Mode: Filament Settings. · · · · · · · · · 85
2.20 Simple Mode: Printer Settings. · · · · · · · · · · 86
2.21 Expert mode speed options. · · · · · · · · · · · 89
2.22 Inll pattern settings. · · · · · · · · · · · · · 92
2.23 Inll pattern: Line (344.51mm / 5m:20s) · · · · · · · 92
2.24 Inll pattern: Rectilinear (350.57mm / 5m:23s) · · · · · 92
2.25 Inll pattern: Concentric (351.80mm / 5m:30s) · · · · · 93
2.26 Inll pattern: Honeycomb (362.73mm / 5m:39s) · · · · 93
2.27 Inll pattern: Hilbert Curve (332.82mm / 5m:28s) · · · · 93
2.28 Inll pattern: Archimedean Chords (333.66mm / 5m:27s) · 93
2.29 Inll pattern: Octagram Spiral (318.63mm / 5m:15s) · · · 94
2.30 Inll pattern comparison in a complex object. Left to Right:
honeycomb, line · · · · · · · · · · · · · · · 94
2.31 Inll patterns at varying densities. Left to Right:
20%,40%,60%,80%. Top to Bottom: Honeycomb, Concentric,
Line, Rectilinear, Hilbert Curve, Archimedean Chords,
Octagram Spiral · · · · · · · · · · · · · · · 95
2.32 Inll advanced settings. · · · · · · · · · · · · · 96
2.33 Retraction settings. · · · · · · · · · · · · · · 97
2.34 Skirt settings. · · · · · · · · · · · · · · · · 99
2.35 Cooling strategy. · · · · · · · · · · · · · · · 101
2.36 Cooling advanced settings. · · · · · · · · · · · · 102
2.37 Support structure options. · · · · · · · · · · · · 104
2.38 Minimug model, tilted 45°. · · · · · · · · · · · · 105
2.39 Support inll pattern: Rectilinear · · · · · · · · · 105
2.40 Support inll pattern: Rectilinear Grid · · · · · · · 105
2.41 Support inll pattern: Honeycomb · · · · · · · · · 106
2.42 Example of pattern angle rotated 45°. · · · · · · · · 106
vii
Page 8
List of Figures
2.43 Multiple extruder options - Printer Settings Tab (General).
Note the two extruders dened in the left-hand pane. · · · 107
2.44 Multiple extruder options - Printer Settings Tab (Extruder). 107
2.45 Plater with multiple lament options. · · · · · · · · 108
2.46 Multiple extruder options - Print Settings Tab. · · · · · 109
2.47 Multiple extruder options - Tool change G-code. · · · · 110
2.48 Extrusion widths options. · · · · · · · · · · · · 111
2.49 Example model highlighting use case for variable layer heights. 112
2.50 Example with normal layer height. · · · · · · · · · 113
2.51 Variable layer height options - Info. · · · · · · · · · 114
2.52 Variable layer height options - Layers. · · · · · · · · 115
2.53 Example with variable layer height. · · · · · · · · · 115
2.54 Example print with variable layer height. · · · · · · · 116
2.55 Example with skipped layers. · · · · · · · · · · · 116
2.56 Saving a prole. · · · · · · · · · · · · · · · 118
2.57 Deleting a prole. · · · · · · · · · · · · · · · 118
2.58 FreeCAD part repair. · · · · · · · · · · · · · 119
2.59 Sequential printing options. · · · · · · · · · · · 120
2.60 The clearance cylinder around an extruder. · · · · · · 121
2.61 Post-processing script option. · · · · · · · · · · · 127
2.62 Example post-processing script to display Slic3r environment
variables. · · · · · · · · · · · · · · · · · · 127
2.63 Example post-processing script to print each line to output. 128
2.64 Extrusion Width. · · · · · · · · · · · · · · · 129
2.65 Bridging lament shape. · · · · · · · · · · · · 130
2.66 Extrusion shape. · · · · · · · · · · · · · · · 131
2.67 No path overlap · · · · · · · · · · · · · · · 131
2.68 Holes made through polygonal segments. · · · · · · · 134
2.69 Z wobble changing layer stacking. · · · · · · · · · 135
2.70 Variable lament diameter changing layer stacking. · · · 135
3.1 GLCD Info Screen · · · · · · · · · · · · · · 143
3.2 Main Menu · · · · · · · · · · · · · · · · · 145
viii
Page 9
WARNINGS
Safety Information
Page 10
WARNING!
Read Me First!
READ THIS MANUAL COMPLETELY BEFORE UNPACKING AND
POWERING UP YOUR PRINTER.
Hazards and Warnings
Your LulzBot™TAZ 3D printer has motorized and heated parts. Always
be aware of possible hazards when the printer is operational.
Electric Shock Hazard
Never open the electronics case when the printer is powered on. Before
removing the electronics case cover always power down the printer and
completely turn o and unplug the power supply. Allow the power supply
to discharge for at least one minute.
Burn Hazard
Never touch the extruder nozzle or heater block without rst turning o
the hot end and allowing it to completely cool down. The hot end can take
up to 20 minutes to completely cool. Never touch recently extruded plastic.
The plastic can stick to your skin and cause burns. The heated bed can
reach high temperatures that are capable of causing burns.
Fire Hazard
Never place ammable materials or liquids on or near the printer when
it is powered on or operational. Liquid acetone and vapors are extremely
ammable.
Pinch Hazard
When the printer is operational take care to never put your ngers in
any moving parts including belts, pulleys, or gears. Tie back long hair or
clothing that can get caught in the moving parts of the printer.
x
Page 11
HAZARDS AND WARNINGS
Static Charge
Make sure to ground yourself before touching the printer, especially its
electronics. Electrostatic discharge can damage electronic components.
Ground yourself by touching a grounded source like your computer case.
Age Warning
For users under the age of 18, adult supervision is recommended. Beware
of choking hazards around small children.
Modications and Repairs Warning
At Aleph Objects, Inc.®we respect your freedom to modify your LulzBot
desktop 3D printer. However any modications or attempted repairs that
cause damage are not covered under the Warranty. Questions? Contact
Technical Support by emailing [email protected], or by calling +1-970377-1111.
™
Federal Communications Commission Statement
Note: This equipment has been tested and found to comply with the
limits for a Class A digital device, pursuant to part 15 of the FCC Rules.
These limits are designed to provide reasonable protection against harmful
interference when the equipment is operated in a commercial environment.
This equipment generates, uses, and can radiate radio frequency energy
and, if not installed and used in accordance with the instruction manual,
may cause harmful interference to radio communications. Operation of
this equipment in a residential area is likely to cause harmful interference
in which case the user will be required to correct the interference at his
own expense.
This device complies with part 15 class A of the FCC Rules. Operation
is subject to the following two conditions:
1. This device may not cause harmful interference and
2. This device must accept any interference received, including interference that may cause undesired operation.
xi
Page 12
WARNING!
FCC Warning: Changes or modications not approved by the party
responsible for compliance could void the users authority to operate the
equipment.
xii
Page 13
3D Printer Software
Page 14
3D Printer Software
1.1 Software Overview
Aleph Objects, Inc., the maker of the LulzBot™TAZ 3D printer, completely
supports Free/Libre software and hardware. Along with the LulzBot
TAZ 3D printer being a Free/Libre hardware design, has been tested to
work with 100% Free/Libre software. Our source code and design les are
hosted on our development server found at http://devel.lulzbot.com.
To operate your desktop 3D printer you will need to install a few software
packages onto your PC. You will need a 3D printer host, an .STL to .gcode
generator, and optional CAD or 3D modeling software.
™
1.2 Software Types
Printer Hosts
Printer Host software is used to control the 3D printer. The program
not only allows you to manually move the printer along all the axes,
but set temperatures manually, send commands, and receive feedback/error messages from the onboard electronics. We recommend
that new users start with Cura as it includes a slicing engine as well.
Common Printer Hosts:
• Cura
• Printrun (Pronterface)
• MatterControl
• OctoPrint
• BotQueue
Slicers
These programs take the 3-Dimensional model (typically
STL/OBJ/etc) and determine the 3D printer toolpath based
on the options selected. The slicing engine uses the nozzle diameter,
movement speeds, layer height, and other variables to determine the
coordinates where it needs to move, and the rates at which it will do
so. This information is exported out of the program as a gcode le.
The gcode le is a plain-text le with a series of text-based codes and
a list of the complete X,Y, and Z axis coordinates used for printing
14
Page 15
1.3. INSTALLING DRIVERS
the 3D model. We recommend that new users start with Cura as it
includes the printer host as well.
Recommended Slicers:
• Cura
• Slic3r
All of the following Free/Libre software packages are available for
GNU/Linux, Windows, and Apple OS X. However, we highly recommend
using these programs on GNU/Linux.
The required software can be found in the Support/Downloads section
at LulzBot.com/support/downloads. You will also nd instructions there
for installing each program onto your PC. You can also nd downloads
specic to the LulzBot™TAZ 3D printer on the LulzBot™TAZ product
page.
1.3 Installing Drivers
Linux and Mac OSX users will not need to install a driver to communicate
with the LulzBot™TAZ 3D printer. Windows users will need to install
the drivers. Using Cura as your printer host and slicing software is
recommended, as the drivers will automatically be installed during the
Cura installation process. The drivers can also be downloaded from
LulzBot.com/support/downloads. A visual guide showing the driver
installation process can be found in our download section as well.
1.4 Cura
Setup Cura
Cura is available for download on our website at
http://LulzBot.com/cura. When installing, it is recommended to
uninstall any previous versions of Cura you may have been using. When
rst opening Cura, you will be prompted to go through the First run
wizard. This will consist of selecting your printer, hot end type, extruder
type, and then your nozzle size.
15
Page 16
3D Printer Software
It is important to select the correct printer, hot end, tool head, and
nozzle size as Cura uses custom proles and machine settings based upon
which printer, hot end, tool head, and nozzle you are running.
• Download the appropriate installer for your computer operating
system. Instructions on installation for each operating system is
available at http://LulzBot.com/cura.
• Install Cura by double clicking on the installer.
• Click through the install wizard until it completes.
• Start Cura by launching it from your list of installed applications.
If this is the rst time that Cura has been used the “Conguration
Wizard” window will open.
• Select LulzBot TAZ 4 or 5, then select Next.
• Select Stock TAZ 5 (PEI and Hex V2). Press Next.
• Choose the correct nozzle size for your machine. Your TAZ 5 comes
with a 0.5mm nozzle standard.
• Select nish.
16
Page 17
1.5. QUICK PRINT SETTINGS
1.5 Quick Print Settings
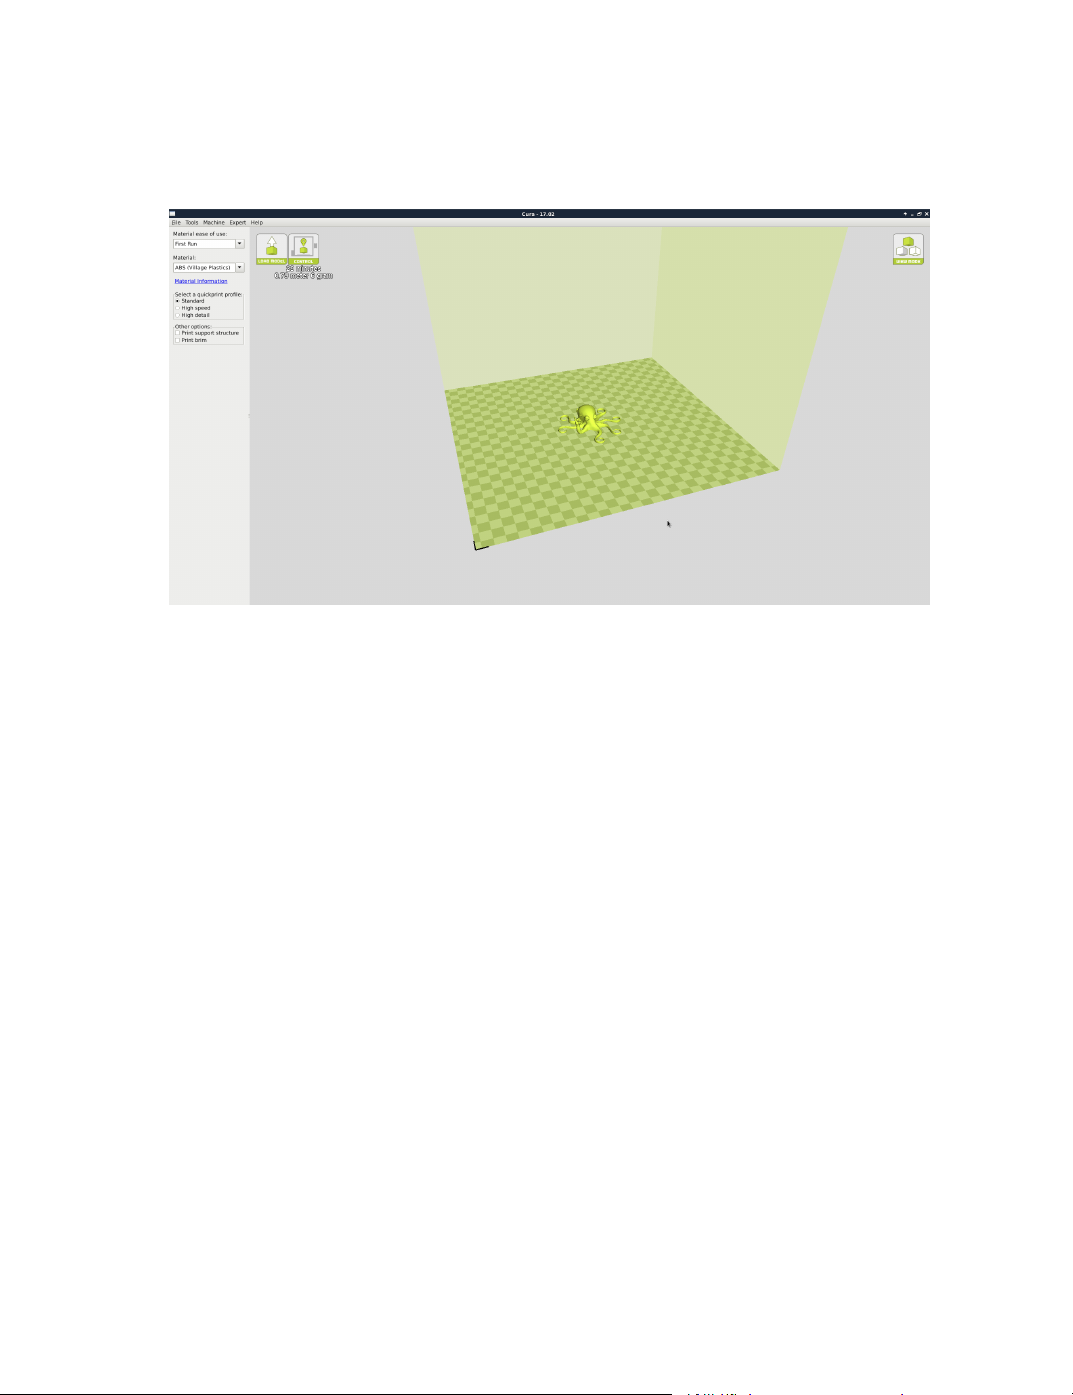
Figure 1.1: Quick Print Settings
After setting up Cura for the rst time, you will be shown the main interface
screen. (Fig. 1.1, page 17):
Selecting a Quick Print Prole
The print quality settings can be found in the top left-hand corner of the
window. For most laments, there will be Standard, High Speed, and
High Detail options. Some of the more exotic laments may only have a
Normal/Standard prole.
High Detail
Designed to give greater detail and ner objects. This will have a
smaller layer height, which will make each layer thinner, so that curves
seem more natural and walls seem less noticeable. This setting will
also require more layers to be laid down, increasing overall print time.
Standard
Designed to give a medium resolution, by increasing the layer height
17
Page 18
3D Printer Software
and print speeds. This will make the organic curves slightly more
step-like than the ne setting, but will reduce printing time.
High Speed
Designed for the fast prints, where overall model nish is not of
concern. Most commonly used for quick iteration of designs found
in rapid prototyping.
Material Selection
Choose your desired lament. The TAZ ships with a 1 meter sample of
ABS, that should be used in your rst print.
Printing Support Material
The TAZ 3D printer is able to print models that have angles and overhangs,
even without support material depending on the overhang distance and
angle. Turn this option on if your model could benet from support
material.
Brim
Brim is used to increase surface area of the part you’re printing, thereby
ensuring proper part adhesion. This will print a single layer high edge
around the outside of the part, helping rst layer adhesion and minimizing
warping.
Load Model File
Select the STL model you would like to print. Either use the Load Model
button or select File > Load Model. Once the le has been loaded, you
will see a 3D rendering of your object on the build platform. Select the
model to see the various options.
Model Orientation
Move your model to change where it is printed on the build plate. Do this
by left clicking on the model and dragging it to the desired location. The
18
Page 19
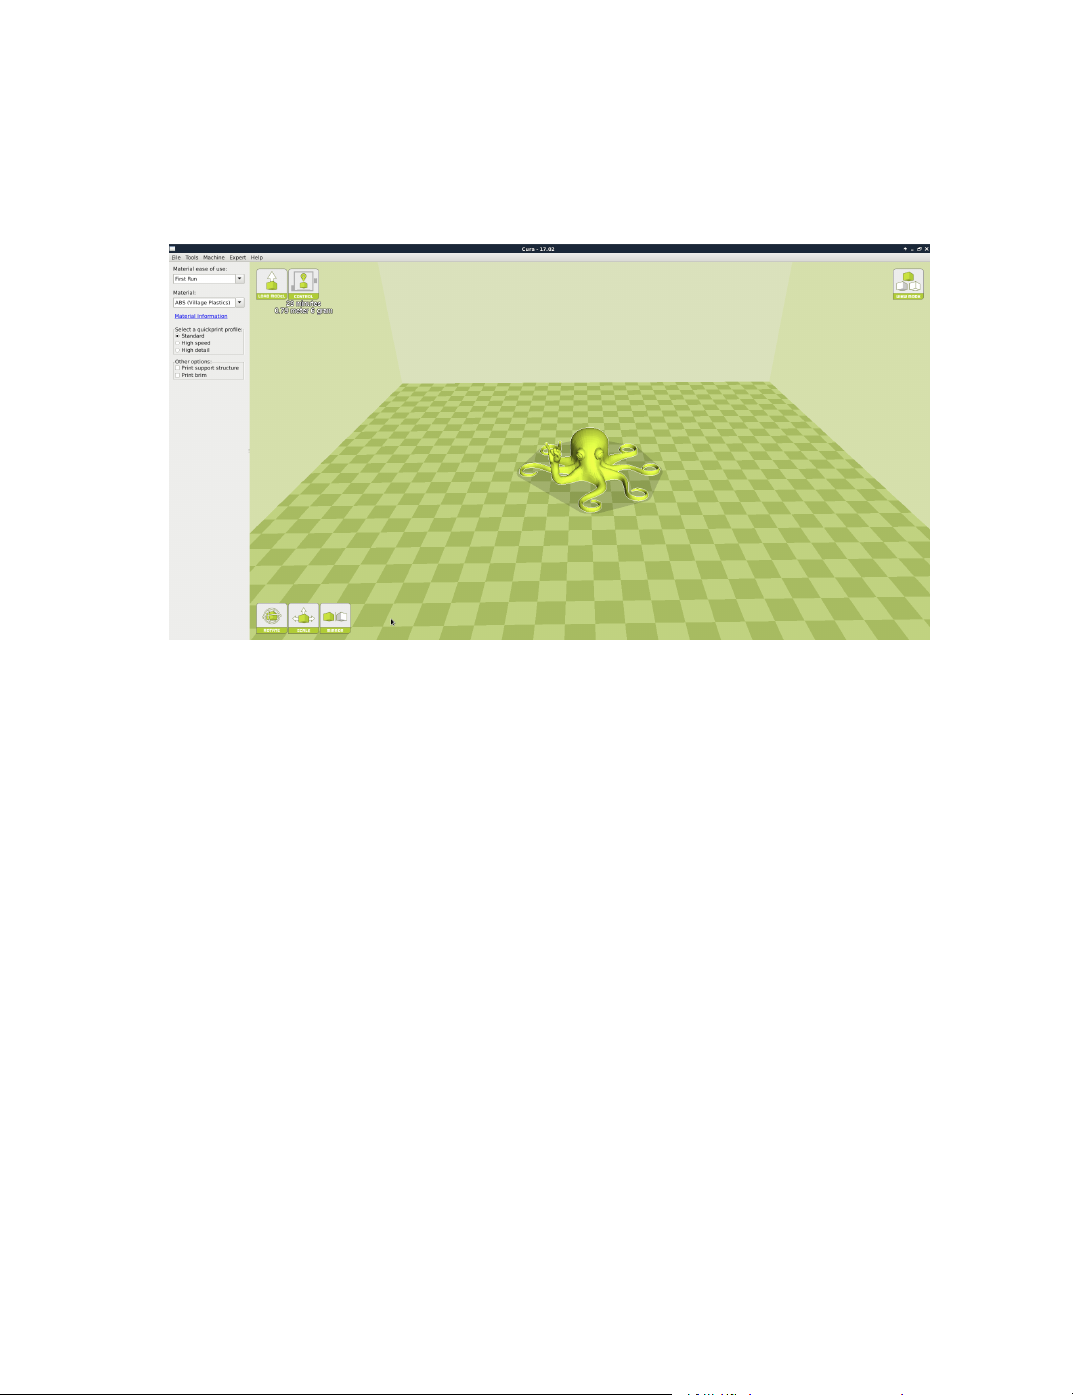
1.5. QUICK PRINT SETTINGS
black outlined corner of the 3D print bed view represents the front left
hand corner of the build plate on your printer. By holding down the right
mouse button and dragging, you can view your model from dierent angles.
Figure 1.2: Options after selecting model
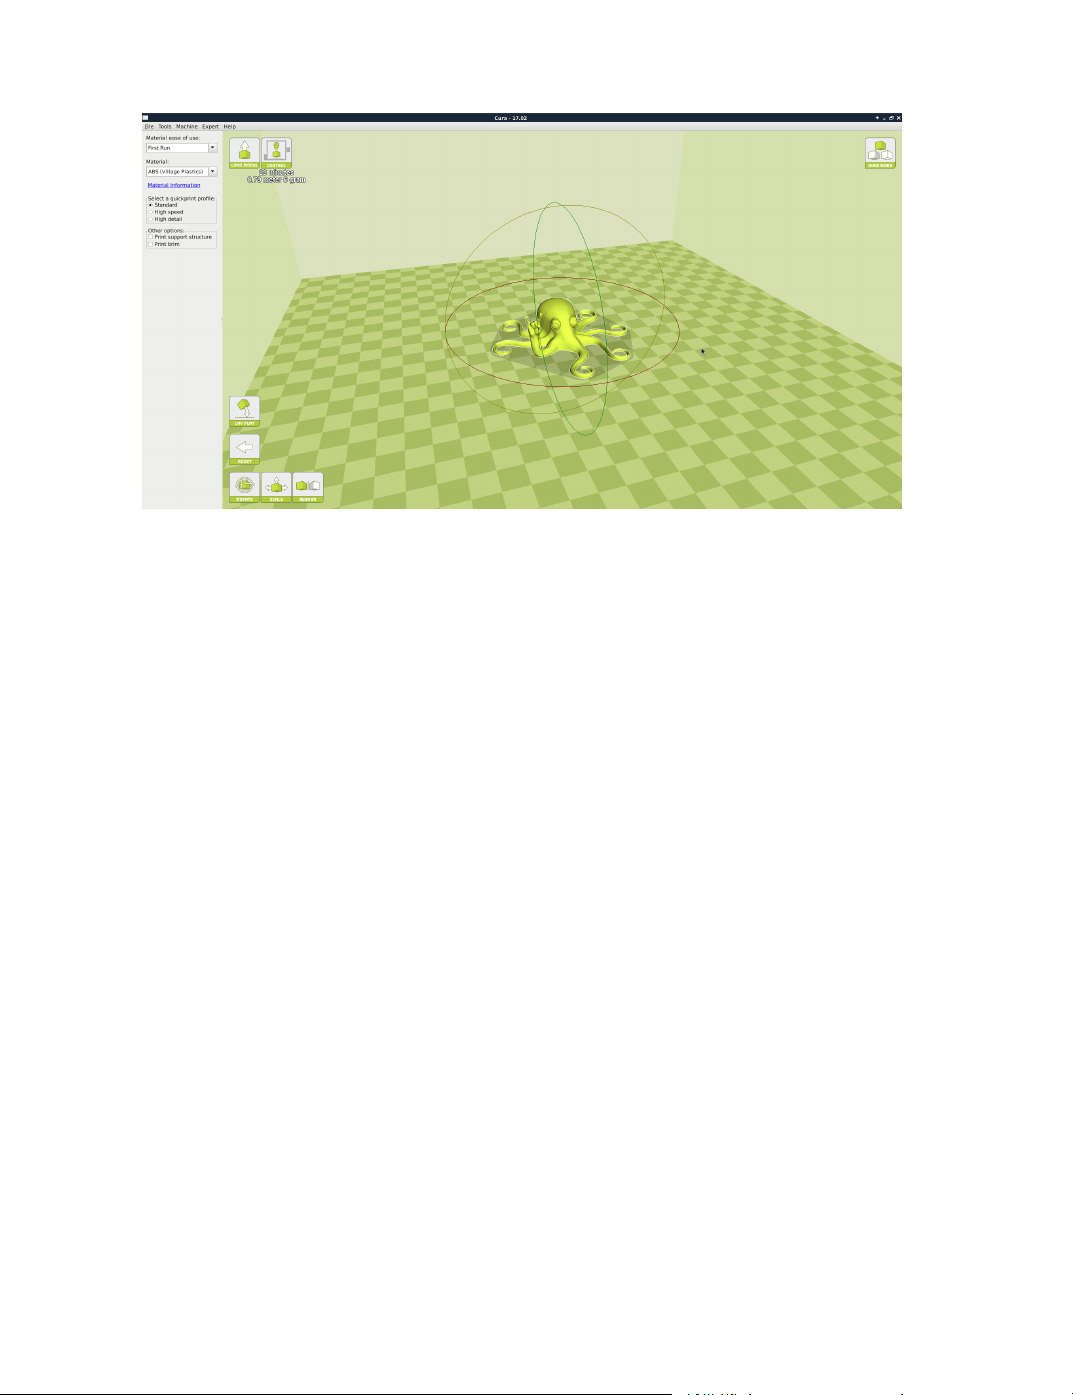
Rotate
The Rotate button will give you the ability to orient your model in along
all three axes. Once you click the rotate button, three circles will surround
your model. The red circle will allow you to rotate around the Z axis. The
Yellow circle will rotate around the Y axis. The Green circle will rotate
around the X axis. Cura defaults to 15 degree increments. Hold Shift to
rotate by One Degree Increments.
19
Page 20
Lay Flat
3D Printer Software
Figure 1.3: Rotating your Model
The Lay Flat button will ensure that the at portion of your print is
securely attached to the bed. It is highly recommended to use this option
after rotating your model in the Z direction, as it will help prevent adhesion
issues during the print.
Reset
The Reset button will return your model to the original orientation as
dened by the CAD program used to create the model.
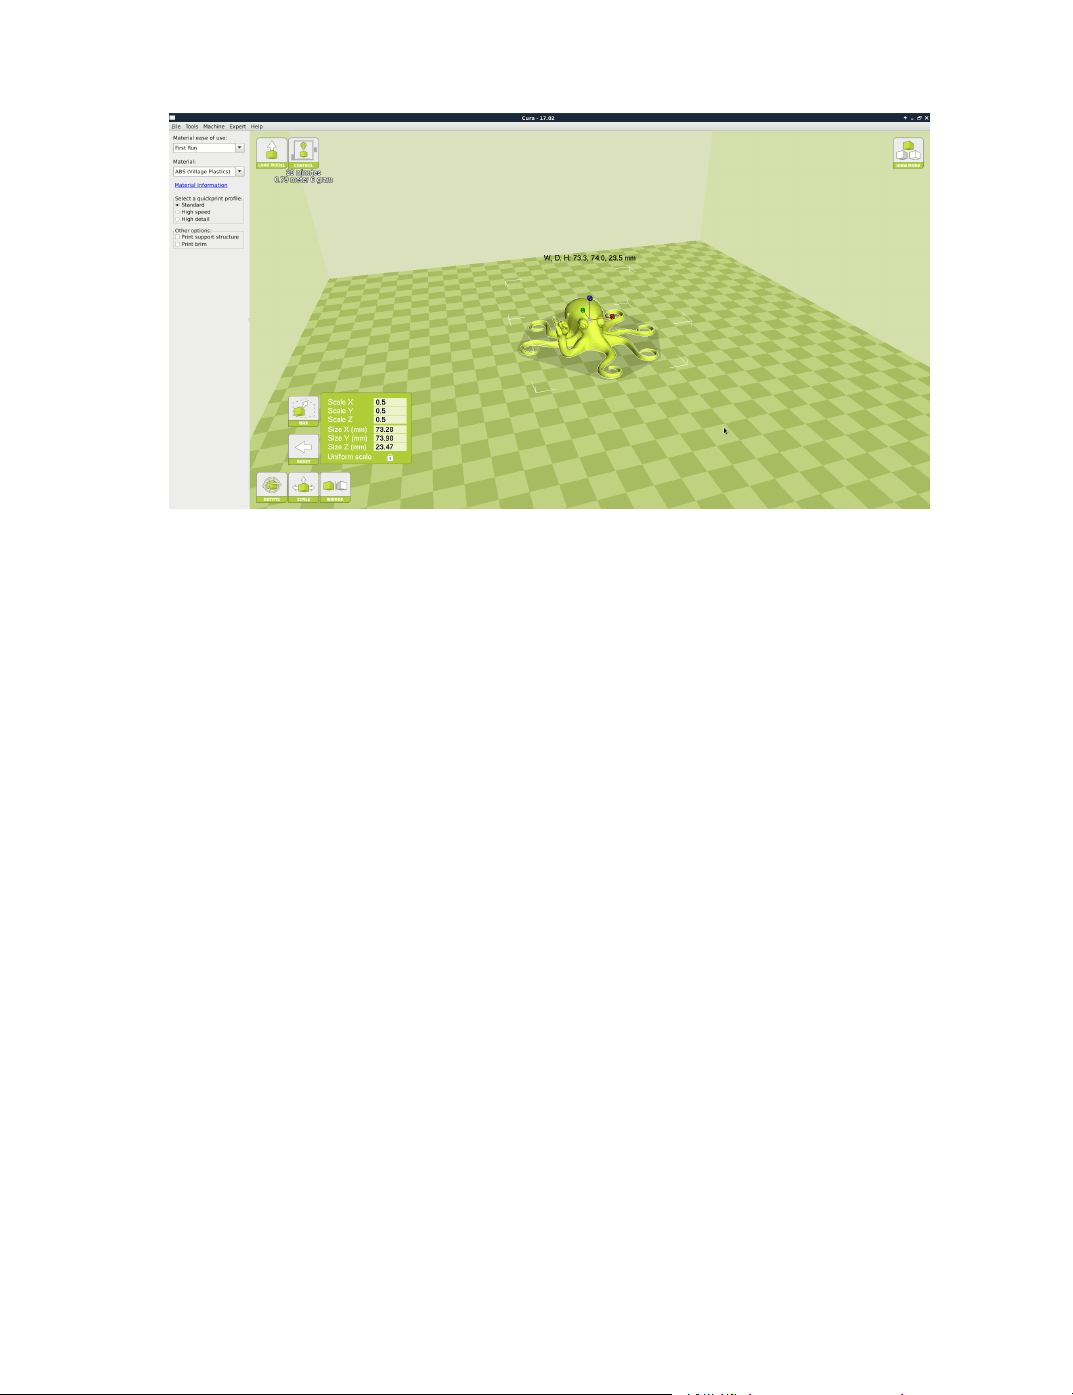
Scale
The Scale button displays the model dimensions, along with the ability to
scale along the X Y or Z axes. Anything below the number 1.0 will reduce
the objects size, while anything above the number 1.0 will increase the
objects size. As a default, it will be set to uniform scaling. This will cause
the X Y and Z axes to be scaled by the same amount when you make a
change to any of them. To disable this, select the lock in the lower section
of the scaling window.
20
Page 21
1.6. VIEW OPTIONS
Figure 1.4: Scaling your Model
1.6 View Options
This mode allows you to view your model in a variety of dierent ways.
This can be helpful for spotting issues before the print even starts.
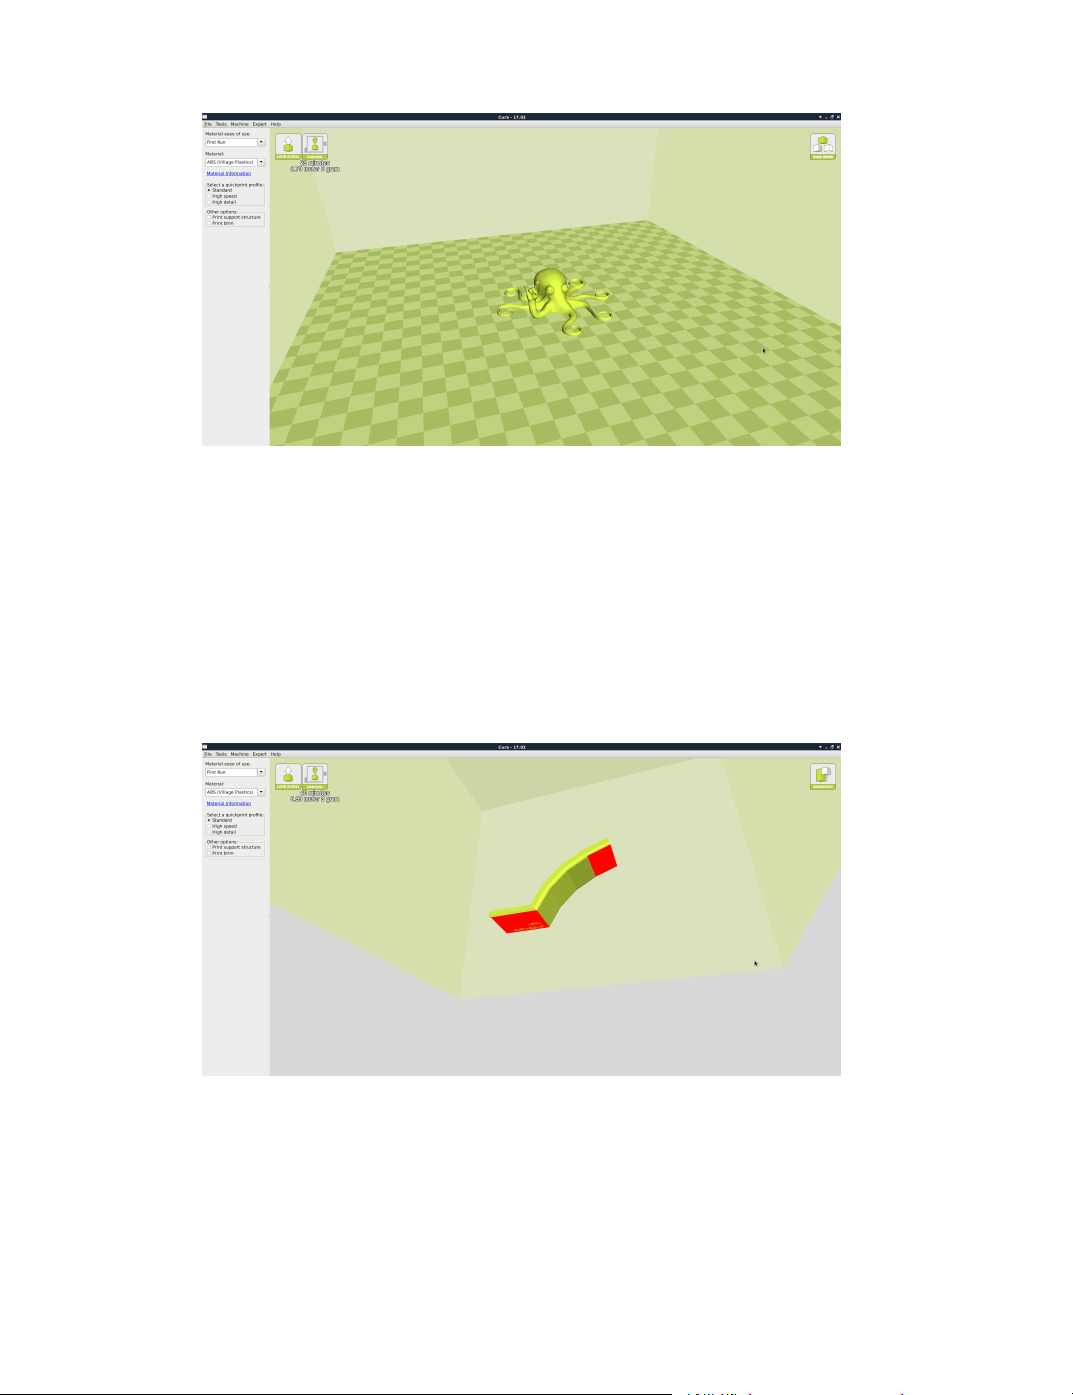
Normal
This is the standard view and shows the solid outer surfaces of the model.
(Fig. 1.5, page 22):
21
Page 22
3D Printer Software
Figure 1.5: View in Normal Mode
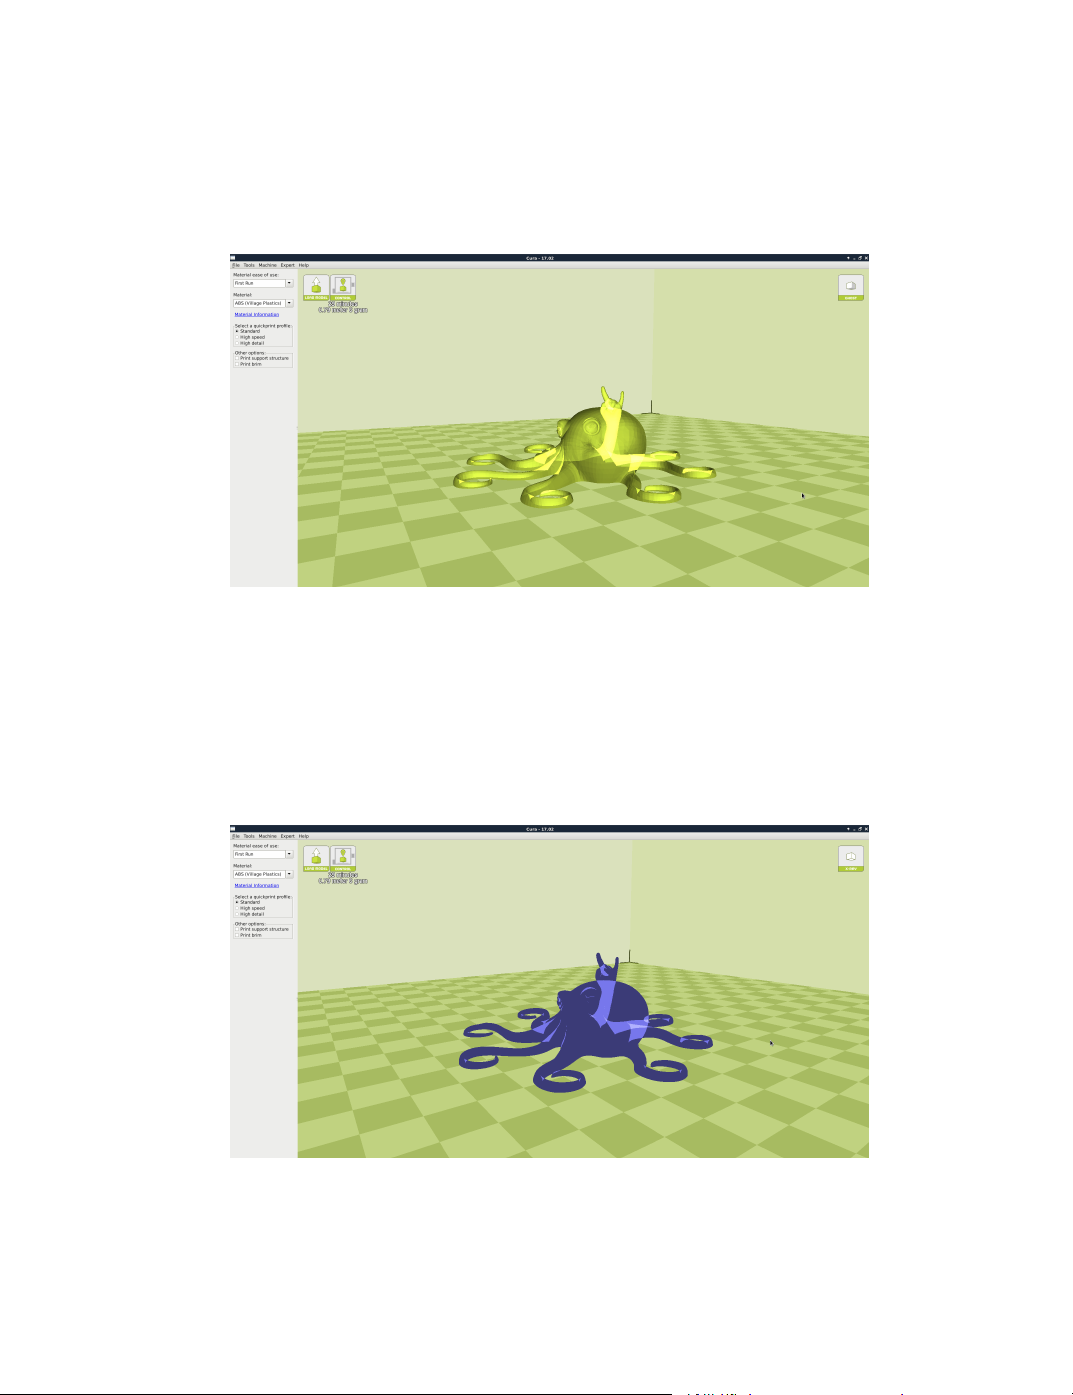
Overhang
Overhang mode shows where your model may need support material. In
Fig. 1.6, page 22 the red highlighted areas show overhangs and more severe
angles and areas where support material is recommended. The overhang
threshold can be dened in Expert Settings.
Figure 1.6: View in Overhang
22
Page 23
1.6. VIEW OPTIONS
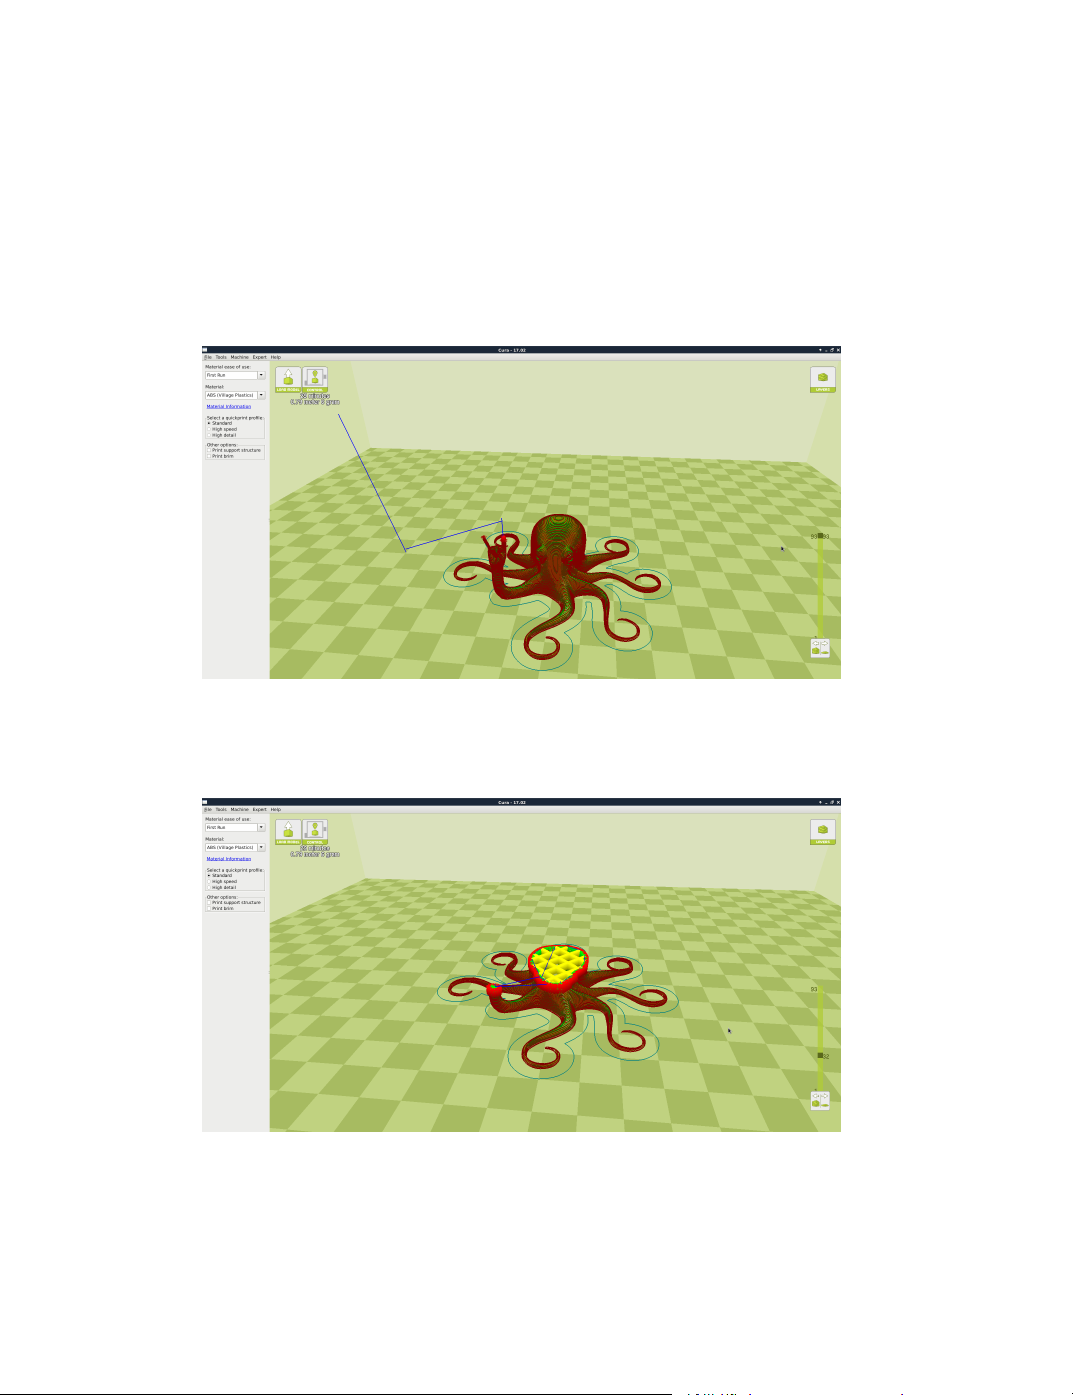
Ghost
Ghost view mode makes the model translucent to allow you to see what is
behind it.
Figure 1.7: View in Ghost
Xray
Xray is very similar to Ghost mode. It will allow you to see into objects,
ensuring that inner details are correct.
Figure 1.8: View in Xray
23
Page 24
3D Printer Software
Layers
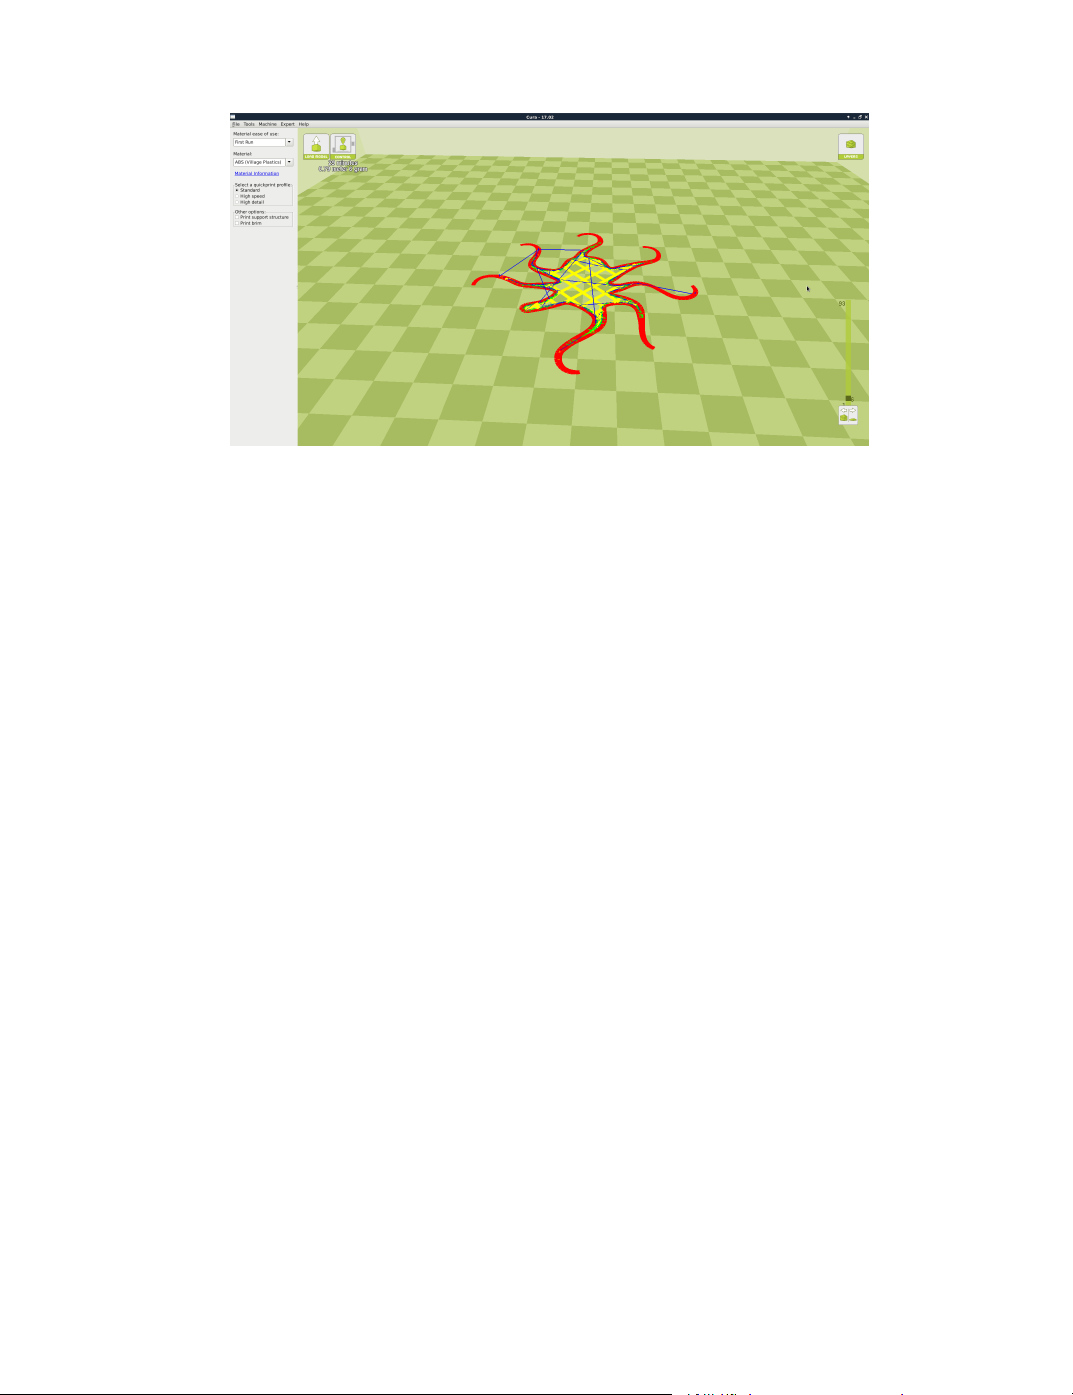
To view the tool path of your print head and to ensure no skipped layers
or gaps use this option. Use the slide bar on the right hand side of the
window to move up and down through the tool path layers. Click the icon
below it to view an individual layer at a time. If there is support activated
in your model, it will be shown in blue.
Figure 1.9: View in Layers
Figure 1.10: Viewing Cumulative Layers
24
Page 25
1.7. STARTING YOUR FIRST PRINT
Figure 1.11: Viewing Specic Layers
1.7 Starting Your First Print
Once you have your model, prole, and lament loaded, it is time for your
rst print!
Your TAZ 3D printer has the ability to print directly from a computer
using the included USB cable, or directly from the SD card by using the
Graphical LCD controller.
Printing from SD Card
Insert the included SD card into your computer. Select File > Save Gcode
and choose the SD card location to save your Gcode le to your SD card.
Insert the SD Card into the Graphical LCD Controller.
Set Temperature
Turn on the heated bed and hot end by using the Graphical LCD controller
and navigating to: Temperature > Select Filament type. If you are
using other materials you can set your desired temperatures by going to
Temperature > Custom Temp > Nozzle/Bed. Wait for your 3D printer to
reach specied temperatures.
25
Page 26
3D Printer Software
Start Print
Once at the desired printing temperature begin your print through your
Graphical LCD controller by navigating to: Print From SD > Desired
File.
Printing from USB Cable
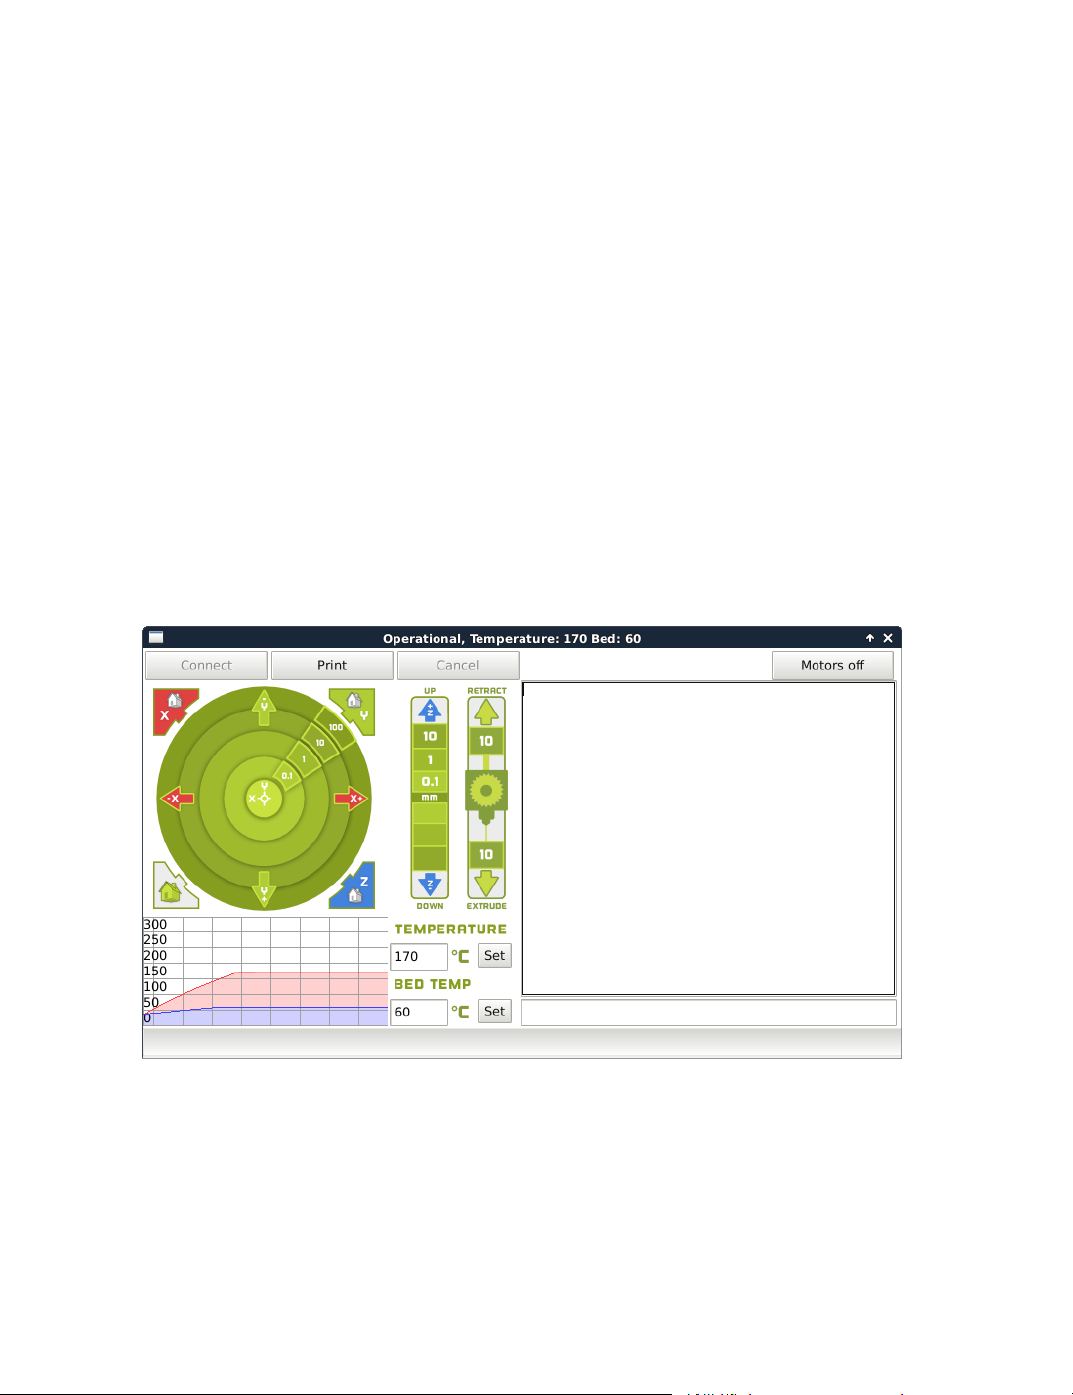
Connect your 3D printer to a computer using a USB cable, power it on
and select the Control button at the top of the 3D viewing window. This
will bring up your Pronterface user interface. You will not be able to send
any commands until the window title changes to Operational. Once it
is operational, you will need to set your lament specic temperatures.
The temperature box heats the hot end, while the bed temp sets the bed
temperature. Your current temperatures will be listed in the top of the
control box. Once your hot end and bed are heated, select Print. This
will start the printing process.
Figure 1.12: Control Screen
26
Page 27
1.8. REMOVING YOUR FIRST PRINT
Recommended Temperatures
When preparing your printer for operation, please be sure to set your
temperatures, in Celsius, to the specic lament you are using.
Filament Type Bed Preparation Nozzle Temp Bed Temp Removal Temp
ABS Clean PEI 240-260 110 50
PLA Clean PEI 195-215 60 45
HIPS Clean PEI 240-260 110 50
Laywoo-D3 Clean PEI 175-195 60 45
Laybrick Clean PEI 175-195 60 45
Magnetic Iron PLA Clean PEI 220-230 60 45
Stainless Steel PLA Clean PEI 220-230 60 45
t-glase Glue stick 240-260 60 45
Flexible Filaments Glue stick 215-230 50 35
Nylons Glue stick 220-270 110 50
Polycarbonate Glue stick 260-300 110 50
Polycarbonate + ABS Glue stick 260-280 110 50
Conductive PLA Clean PEI 215-230 60 50
N-Vent Glue stick 220-260 110 50
1.8 Removing Your First Print
After your rst print has nished, you need to wait for the part to cool
down. Your parts will be easier to remove if you allow your heated bed to
cool down to optimal temperature. This will allow the plastic to contract,
making it easier to remove.
Once your heated bed has cooled, use the blue handled knife that was
included with your toolkit to remove the item. Carefully insert the blade
of the knife between your print and heated bed. Once underneath the part
rotate the blade lifting with the sharp edge into the part, to gently pop the
piece o your plate.
27
Page 28
3D Printer Software
1.9 Full Settings
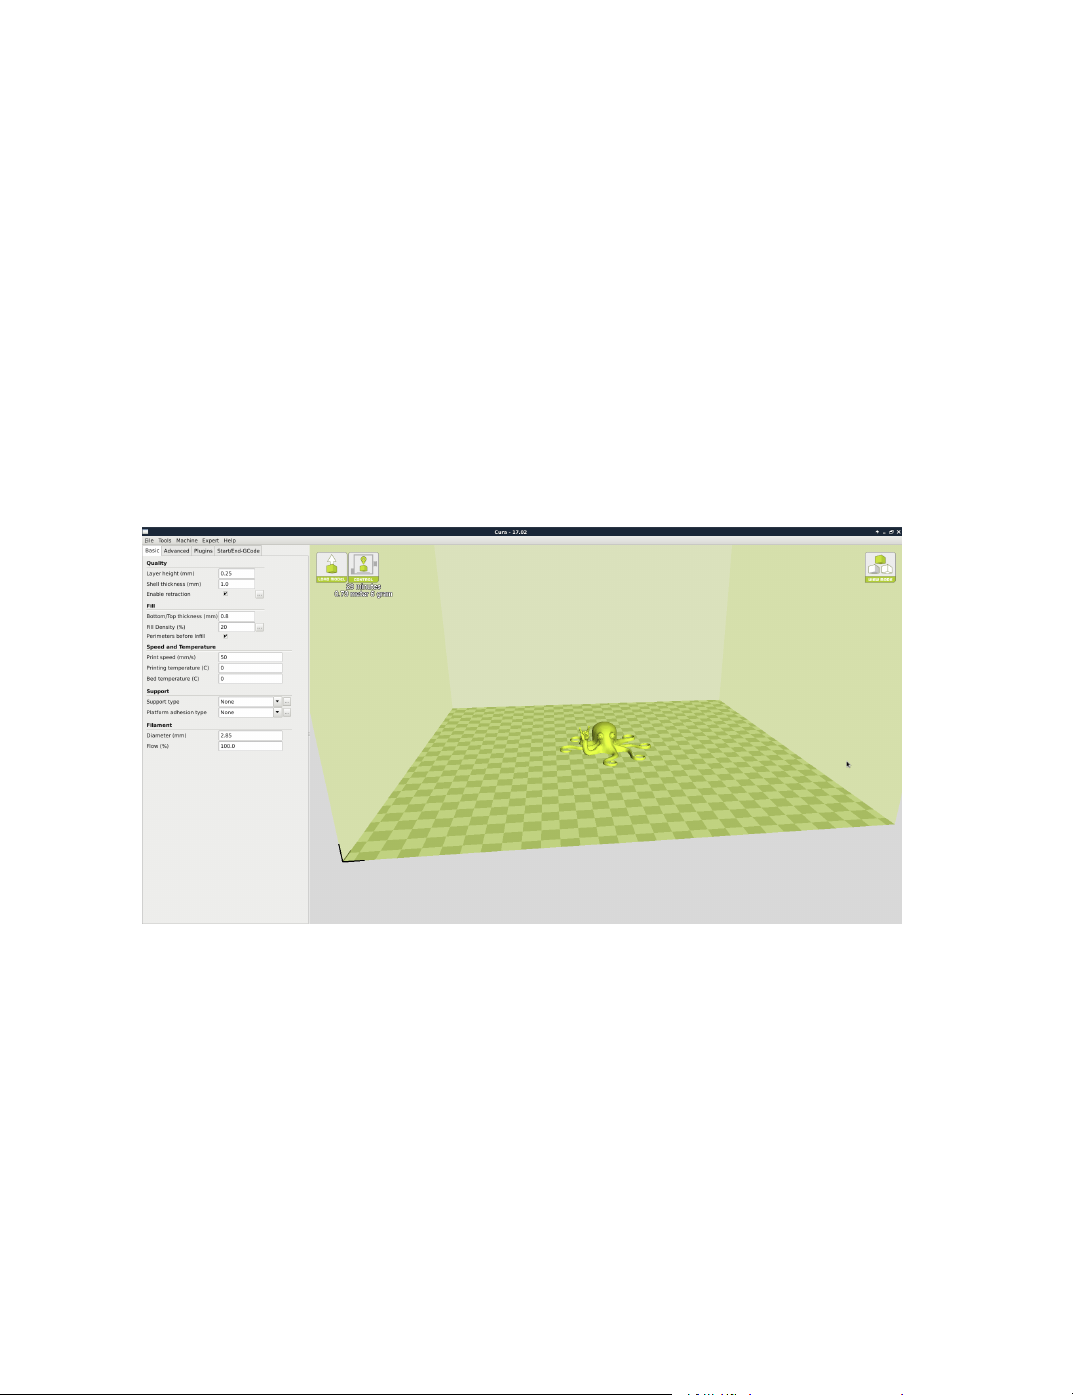
Full settings should not be used until enough experience with 3D printing
has been gained to feel comfortable with all aspects of the printer and its
operation. The Quickprint Mode will provide good results for most models.
The rst time Cura is launched it will default to the Quick Print interface.
In order to have more control of your slicing and Gcode generation, switch
to Full Settings. Choose your desired Quick Print prole, as you can
copy over the current settings when changing to “Full Settings” mode. This
will automatically update the settings for that lament. Select Expert >
Switch to full settings. The following tabs will now be available:
Basic, Advanced, Plugins, and Start/End-Gcode. You will also have access
to the Expert Settings.
Figure 1.13: View in Full Settings
View in Full Settings
When you rst switch to Full Settings, Cura will need to know what lament
and quality you wish to use. It will automatically transfer our quickprint
settings over to allow adjustments if one is selected. IF A QUICKPRINT
PROFILE IS NOT AVAILABLE, YOU WILL NEED TO MANUALLY
LOAD ONE. We recommend using our tested proles that are available
28
Page 29
1.10. BASIC TAB OPTIONS
here: https://www.lulzbot.com/cura. You will want to choose the
prole that matches your lament and quality needs. Once downloaded,
you can load the le into Cura by selecting File > Open Profile. Choose
your desired prole. This will automatically update all of your settings for
use with your printer.
1.10 Basic Tab Options
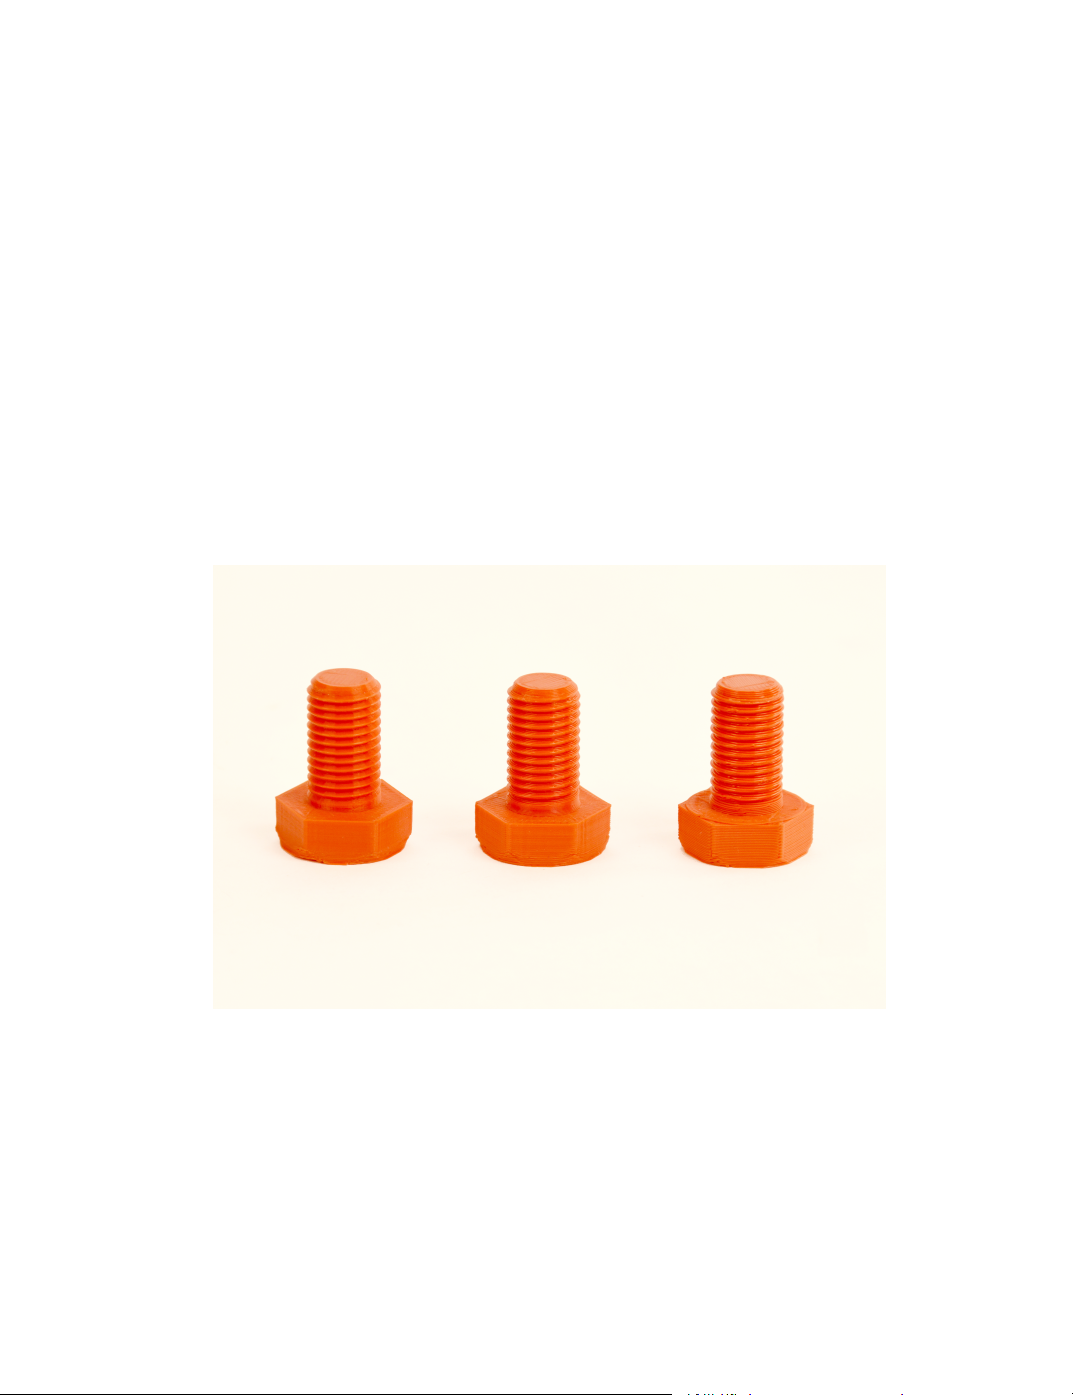
Layer Height
The thickness of each printed layer is known as the “Layer Height”. The
smaller the layer height, the smoother curves will appear. Larger layer
heights are better for bridging and overhangs. Smaller layer heights will
also increase print time, as it will take more layers to complete the object.
Figure 1.14: Dierences in Layer Height
Shell Thickness
This denes the number of vertical walls that comprise the outside of your
model. We recommend keeping this set to multiples of your nozzle width.
29
Page 30
3D Printer Software
Your TAZ 3D printer is equipped with a 0.5mm nozzle.
Enable Retraction
Retraction tells your printer to pull lament out of the hot end upon travel
moves. Travel moves are when your print head moves from one area of the
print, to another without laying down lament. We recommend keeping
this on for all lament types, and adjusting the retraction length and speed
for the specic lament.
Bottom/Top Thickness (mm)
Also known as “Surface Layers” this will determine how thick the top and
bottom layers are. A larger number here will create a thicker top and
bottom which can be helpful for strength, bridging, and quality purposes.
We recommend keeping this number as a multiple of your layer height.
Fill Density
This number is expressed as a percentage. 0% will give a completely hollow
print, while 100% will give you a completely solid object. We have found
that 20% to 40% ll density is functional for most prints.
Perimeters Before Inll
This option will toggle in what order the inll and perimeters are printed.
We recommend leaving this toggled.
Print Speed (mm/s)
Your overall printing speed can be adjusted here. If no other speeds are
determined in the later sections your printer will automatically default to
this speed. This speed will be dierent, depending on what type of lament
you are using.
Printing Temperature
We recommend leaving this temperature setting to “0”. If you set your
temperature in this section your printer will not begin printing until it
30
Page 31
1.10. BASIC TAB OPTIONS
reaches the EXACT temperature. We recommend setting your printing
temperatures through the Printer Interface, or through your LCD.
Bed Temperature
We recommend leaving this temperature setting to “0”. If you set your
temperature in this section your printer will not begin printing until
it reaches the EXACT temperature. We recommend setting your bed
temperatures through the Printer Interface, or through your LCD.
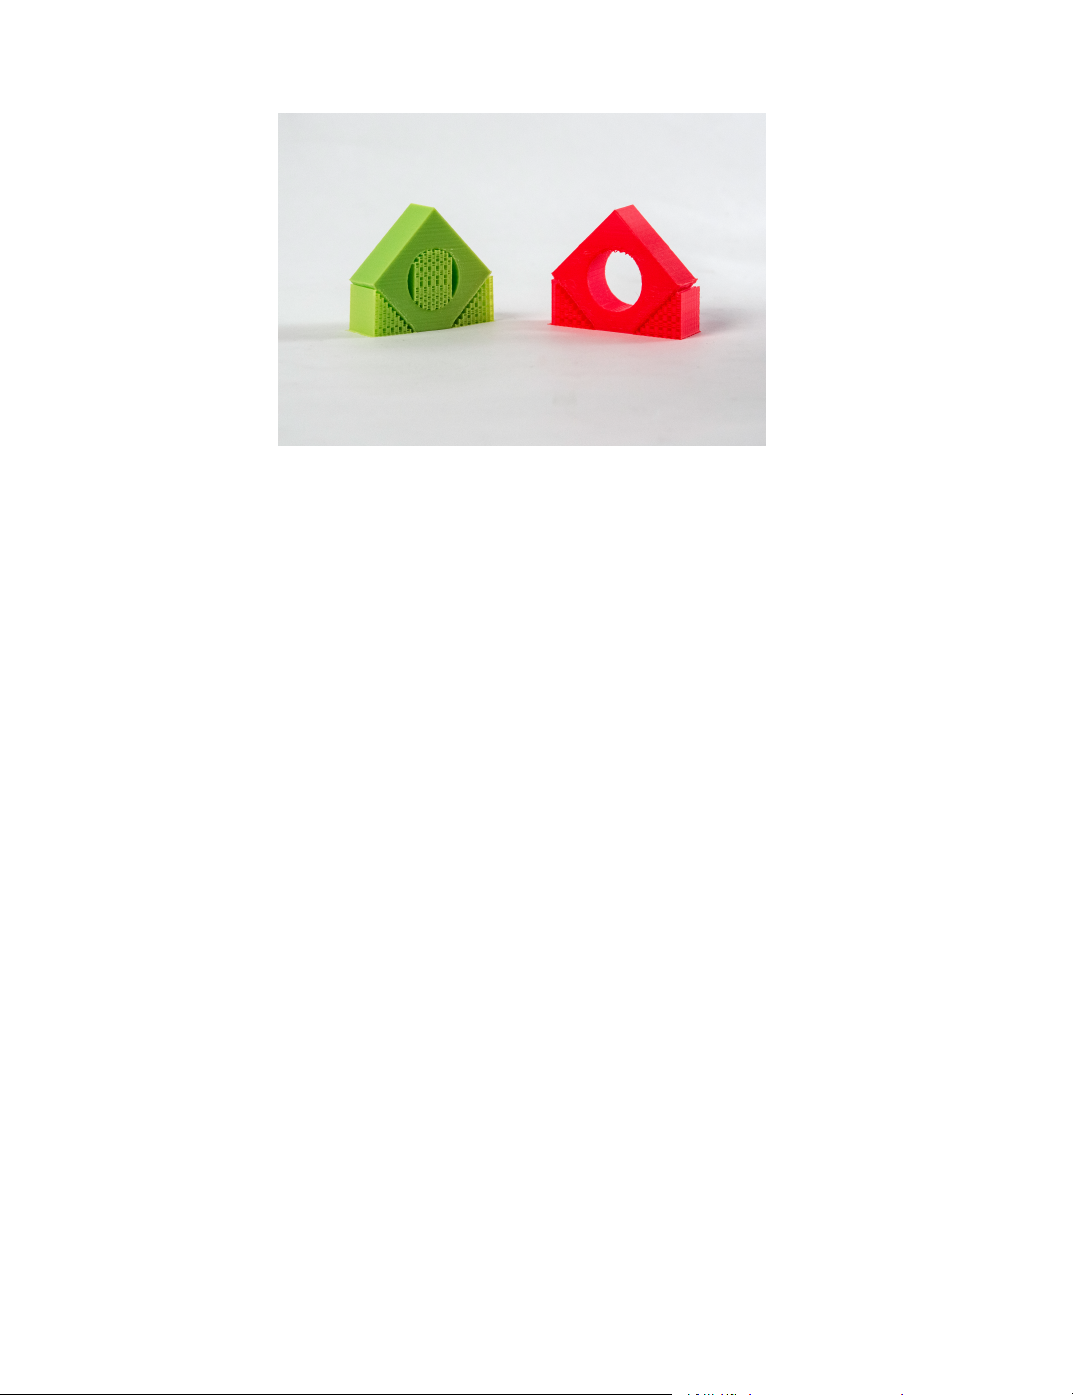
Support Type
Some models will require support material in order to print properly. This
will usually occur when an object has an angle in relation to the build plate
between 0 to 45 degrees. It is highly recommended to orient your object so
that it minimizes or eliminates the need for support.
Touching Buildplate
This causes the support material to build up between the heated bed and
the object. The red example is Touching Buildplate.
Everywhere
This prints support material between the heated bed and object as well as
between the object and itself. The green example is Support Everywhere.
31
Page 32
3D Printer Software
Figure 1.15: Support Types
Platform Adhesion Type
Some models have a small surface area contacting the plate. This can
create adhesion issues causing your part to pop o at some point during
the print. To x this, use either Brim or Raft. Raft is better used when a
model has small heated bed contact points and overhangs.
Brim
Brim will create a single layer of lament, contacting and surrounding your
model. This will increase the surface area of the part contacting the build
platform thereby preventing it from popping o the heated bed. Brim will
also help in situations where you are seeing corner lift. Brim settings can
be adjusted in the Expert Settings options.
Raft
Raft will generate a layer of material underneath your object. Raft was
more often used before the addition of heated plates to increase surface
area. Raft settings can be adjusted in the Expert Settings options.
32
Page 33
1.11. ADVANCED TAB OPTIONS
Filament Diameter
The lament diameter setting is one of the more important settings. Make
sure that you update this value periodically with your average lament
diameter. While your lament may be referred to as 3mm, it is more
likely going to be near 2.9mm +/- 0.1mm. You will want this to be an
accurate average, as it will allow your printer to correctly calculate how
much lament it is pulling into the hot end.
Filament Flow %
This controls how much lament your printer is extruding in relation to
speed. This setting is mainly used to adjust for lament density variations.
Leave this value at 100% as changing it can lead to surface quality issues.
1.11 Advanced Tab Options
Nozzle Size (mm)
This denes your nozzle size. The slicing engine uses this value combined
with your other settings to determine how quickly to feed lament into your
hot end. The TAZ ships with a 0.5mm nozzle.
Retraction Speed (mm/s)
Retraction Speed determines the speed at which your lament is reversed
out of the hot end for travel moves and when changing direction during
printing. We recommend keeping this set to 25mm/s or lower.
Retraction Distance
Retraction Distance determines how much lament is pulled out of your hot
end on travel moves and when changing direction. You will want to adjust
this depending on temperature settings and lament type. Higher thermal
retaining laments such as PLA behave better with a longer retraction
distance. We have found anywhere from 1mm to 3mm is a good starting
range.
33
Page 34
3D Printer Software
Initial Layer Thickness
This will control how thick your rst printed layer height is printed onto the
heated bed. Having a larger initial layer height will help prevent your part
from popping o the plate. All of our standard proles have a 0.3mm initial
layer height. This eliminates the need for adjustments when switching
between laments.
Initial Layer Line Width
This will control how wide your rst extruded lament path is for the initial
layer. A wider line width will help with bed adhesion. We have found 125%
to be a good starting place. For models with moving printed in place parts,
a smaller initial layer line width is recommended.
Cut O Object Bottom (mm)
This setting is used to help print models that were not specically designed
for FFF printing. In particular, it is for models that do not have a at
surface to adhere to the plate. It will sink your object Xmm into the build
plate, creating a nice at surface to begin your print. You can also use this
option to remove the lower portion of your model, or if carefully measured,
cut your part in half for printing object as two halves.
34
Page 35
1.11. ADVANCED TAB OPTIONS
Figure 1.16: Cuto Example
Dual Extrusion Overlap
This will determine how far your Dual Extruders will overlap when laying
down material. This will help adhesion between the two dierent colors or
types of lament. This setting is only used when the printer is equipped
with two hot ends and extruders.
Travel Speed
This setting will determine how fast your print head moves while not extruding lament. A normal travel speed of 125 - 175mm/s is recommended.
Bottom Layer Speed
This will control your initial layer speed. In general, a slower initial layer
speed will help with rst layer adhesion.
Inll Speed
This is how fast your print head speed will be while laying down the interior
portion of your model. Faster speeds are usually tolerable here, as none of
35
Page 36
3D Printer Software
the inll will be visible from the outside of your object. If you go too fast
compared to your inner and outer shells, you can have adhesion issues or
globs of lament left behind from the print head.
Outer Shell Speed
This will be the outermost surface of the model. This is the most important
speed setting, as it controls the speed of your print head on the visible layers.
As a general rule of thumb, the slower you go the better looking print you
will get.
Inner Shell Speed
This aects vertical walls that are in between the outer shell and inll. This
will not be visible but will help support the outer shell and the inll. We
recommend keeping this speed setting between your inll and your outer
shell speed.
Minimal Layer Time
This will determine a minimum amount of time your printer will spend
laying down each layer. If your layer print time falls below this your printer
will automatically slow down to reach this time before moving onto the next
layer. Tweaking this can help get cleaner, crisper prints.
Enable Cooling Fan
Enables operation of your extruder active cooling fan. The fan settings can
be adjusted in the Expert Settings options.
1.12 Plugins
Plugins are custom settings which will alter your print at specic
points. The two that come preloaded with Cura are Tweak at Z, and
Pause at Height. More plugins and information can be found here:
http://wiki.ultimaker.com/Category:CuraPlugin To activate one of
36
Page 37
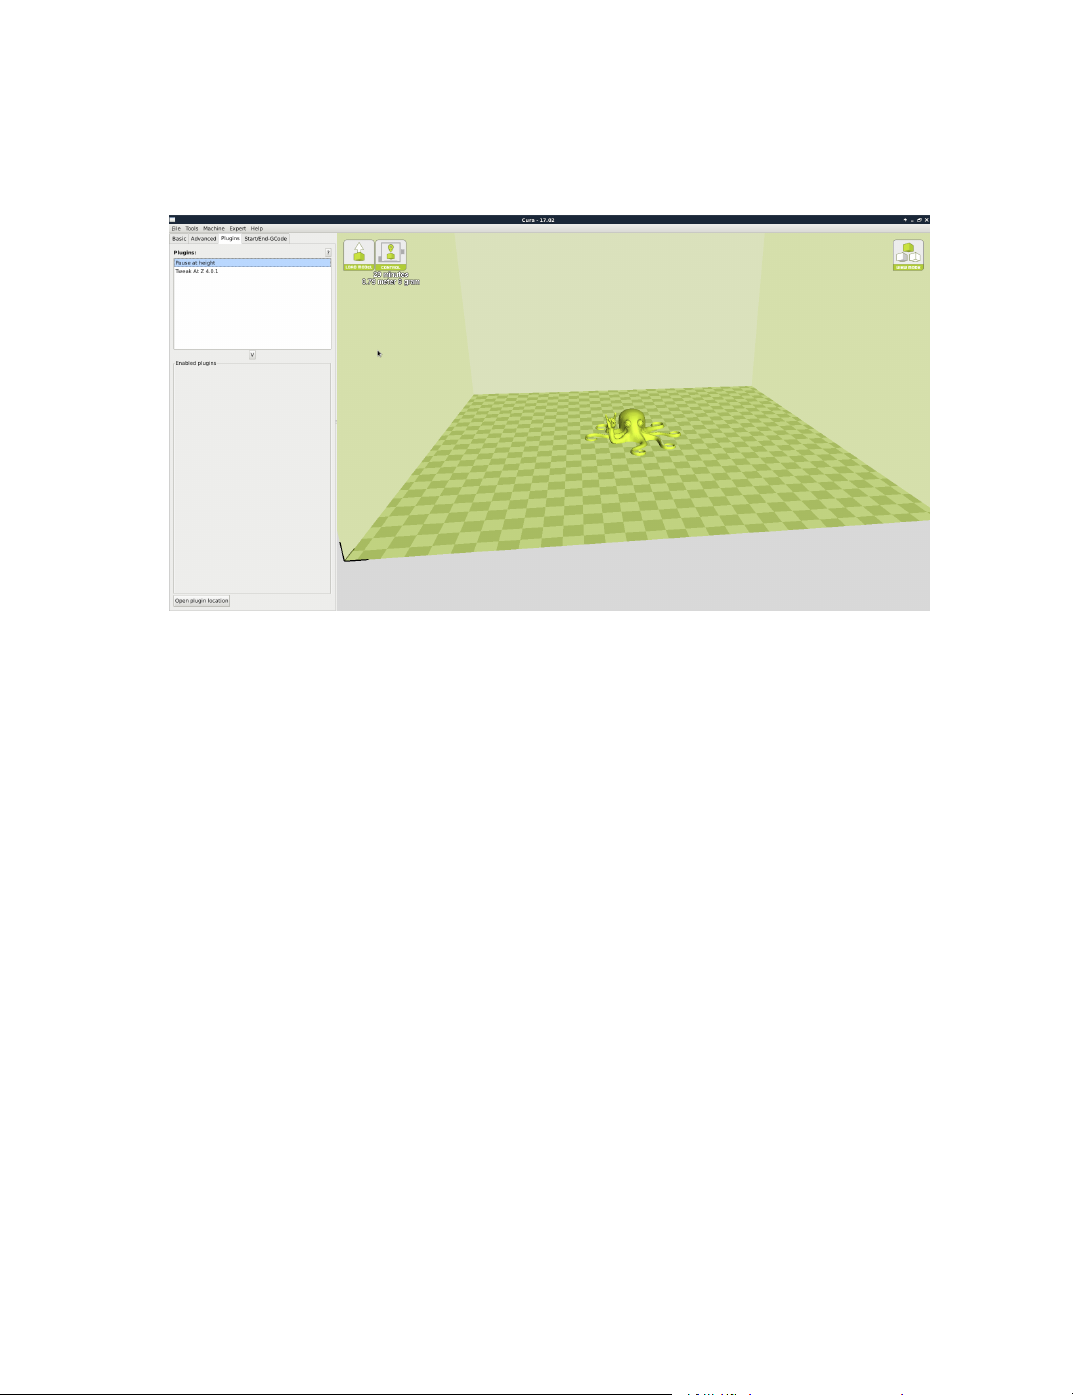
1.12. PLUGINS
these highlight the desired plugin and click the drop-down arrow directly
below the Plugins box.
Figure 1.17: View of Plugins
Tweak at Z
Make basic changes at specied Z heights. You can determine the Z height
or layer count at which you want to make a change. Then choose how you
would like to change your settings. You can alter temperatures, fan speeds,
and print speeds. Fine tuning these for specic STL les, can produce
cleaner prints.
Pause at Z Height
Pause your print at a specied height. You can also specify where to
move the print head and how much lament to retract. This will prevent
“blobs” from accumulating on your print while paused. This setting is most
commonly used when switching colors of laments in the middle of a print.
37
Page 38
3D Printer Software
1.13 Start and End Gcode Settings
Custom Gcode allows for complex automatic printer movements and op-
erations. By adding custom Gcode into the start or end of your le, you
can alter how it prints. A comprehensive list of Gcode commands can be
found here: http://reprap.org/wiki/G-code We recommend new users
to leave this as provided in the proles at https://www.lulzbot.com/cura
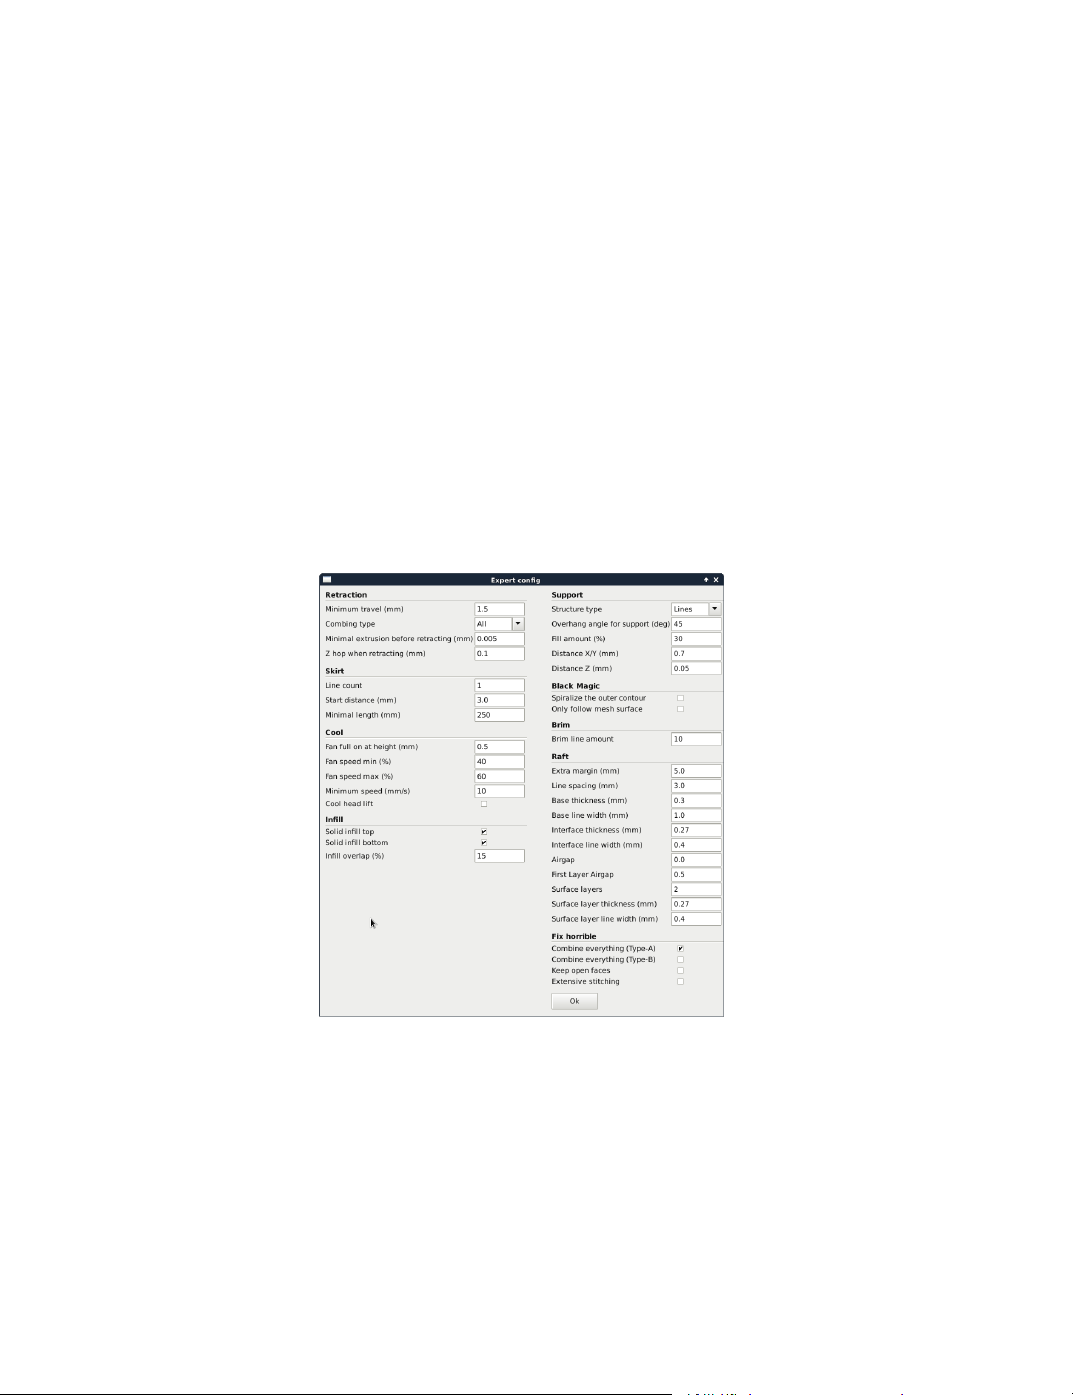
1.14 Expert Settings
Expert settings will give you more specic options for your retraction, skirt,
active cooling, inll, support, brim, raft, and special settings. To gain
access to this section you go to Expert > Open Full Settings or on your
keyboard press Control + E.
Figure 1.18: View Expert Settings
38
Page 39
1.15. RETRACTION
1.15 Retraction
Retraction pulls lament out of your nozzle when it is not extruding to
prevent your print head from dripping on your object. This section is
where you will control how your extruder retracts its lament.
Minimum Travel
This sets the minimum travel distance of your print head in order to retract.
If your print head is not moving this far during travel moves, it will not
retract.
Combing
This option prevents your print head from traveling over holes in the
X/Y plane when printing. This will slightly increase print time, but will
prevent strings from getting caught on the holes during travel moves. We
recommend keeping this setting on.
Minimal Extrusion Before Retracting
This will prevent a retraction move, if your extruder has not put out Xmm
of lament since its last retraction.
Z Hop When Retracting
This will raise your print head Xmm while retracting. This setting helps
prevent ooze, and strings from being deposited on your print.
1.16 Skirt
Skirt creates a line around the outside of your object. Most commonly used
to prime the extruder, in order to prevent missed lament at the beginning
of a print. Leave this setting on.
39
Page 40
3D Printer Software
Line Count
This will dene the number of loops the Skirt creates around the outside
of your object. Smaller models will require more loops to properly prime
the extruder.
Start Distance
This will dene the distance away from your model that the skirt will be
created.
Minimal Length
This will dene the minimum extruded line length for the skirt. This will
over ride your line count, producing as many lines as required to reach the
minimal length.
1.17 Cool
This section will dene how your extruder cooling fan will operate during
the print. Your fan will not start until it has reached 25% or higher for
speed settings. If your print speeds are slowed down due to minimal layer
time, the fan will run between minimum and maximum speed based upon
how much the layer is slowed down.
Fan on at Full Height
This is your Z height where your fan will be turned on to its minimum
percentage setting. Especially helpful with high temperature retaining
laments such as PLA. This will be scaled between 0%, and your minimum
fan speed based upon layer height; with it being disabled for the rst layer.
Fan Speed Min
This will be the speed your fan runs when enabled at full height. Once the
Z height is reached for Fan on at Full Height, this will be the speed your
fan runs at.
40
Page 41
1.18. SUPPORT
Fan Speed Max
This is the fastest speed at which your fan will ever run. When your print
speed is slowed down due to minimal layer time, your fan will run between
minimum and maximum speed. The maximum fan speed is reached when
your printer must be slowed by 50% or greater.
1.18 Support
You dene how your support material is generated here. You must have
some form of support turned on in the basic settings in order for these
settings to have an eect.
Structure Type
You can choose between a Grid or a Line pattern for your support material.
The grid will be a checkerboard pattern in the X and Y direction. The
line option will produce lines in along the y axis for support. The grid
will provide stronger support than the line option, but will be harder to
remove.
Overhang Angle for Support
This will determine where support material is generated. In general you
will be able to print a model with 45 to 90 degree angles in relation to the
bed without support. We recommend leaving this setting at 45 degrees.
Fill Amount
This will determine how dense your support material is printed, similar to
Inll Percentage. The higher percentage, the better support, but it will
be harder to remove the support material, will use more material, and will
lead to a larger total printing time.
Distance X/Y
This will determine how far away from your object in the X/Y plane that
the support material is being placed.
41
Page 42
3D Printer Software
Distance Z
This will determine how far away your support material is from your object
in the vertical direction. A smaller number here makes for better support,
but makes it harder to remove.
1.19 Black Magic
This section allows you to transform your model into a hollow shell, a single
layer thick.
Spiralize the Outer Contour
This causes your Z axis to be constantly moving upward as printing your
single outer wall shell. The results are no layer change lines, giving a much
smoother surface. This setting is typically only used for artistic objects as
they will be fragile.
Only Follow Mesh Surface
This will cause your print to follow the outside of your model, building
it completely hollow with a single wall outer shell. The only dierence
between this and Spiralize, is that the Z axis moves regularly. That is, it
prints a layer and then moves up to the next one.
1.20 Brim
Brim circles the base of the print while making contact, helping adhere
the print to the heated plate. This is only one layer thick, and easily
removed post-print. This section denes how the brim is formed when
brim is activated in basic settings.
Brim Line Amount
This will determine the distance the brim will cover around the outside of
your object. The more brim used, the better your part will adhere to the
plate.
42
Page 43
1.21. RAFT
1.21 Raft
Raft is a platform built underneath your object, designed to help adhesion
and prevent warping. It will lay down support material, and then a
platform on top of the supports. Your model will be built on top of this
platform. The bottom surface of your printed part will not be as clean or
as even when using this option. Raft is typically not required.
Extra Margin
This determines the distance around the outside of your object that the
raft is created. Can be helpful for ensuring no warping of the lower layers.
Line Spacing
This will determine the spacing between “support” lines for the raft. A
small spacing makes the support structures closer together improving
strength of the raft, but uses more material.
Base Thickness
This denes how thick your raft will be.
Base Line Width
This will dene how wide your “support” material is for the raft. This
setting will determine how well the surface layers of the raft print.
Interface Thickness
This will determine how thick the surface layers of the raft are. The surface
layers are the platform that is built upon the supports.
Interface Line Width
This will determine how wide the top layers of the platform will be. In
general, you can keep this set to your nozzle size, as surface quality of the
removable raft is not important.
43
Page 44
3D Printer Software
Airgap
This will dene the distance between your raft and your print. A larger
gap will make your part easier to remove, but will make the bottom of your
print look worse.
Surface Layers
This will determine the number of layers that create the “platform” of your
raft. If you have a wide line spacing, you may want to increase this number
to ensure a solid platform.
1.22 Fix Horrible
These are some of the more advanced and experimental options. They are
designed to help repair models with errors to make them suitable for 3D
printing. They do not always work. Please be cautious when using these
options as they can have unintended eects on your print quality.
Combine Everything (Type-A)
This will attempt to x all external mesh errors, while keeping internal
holes intact. This can accidentally ll in intentional internal holes.
Combine Everything (Type-B)
This will ignore all internal holes of the model and only focus on the external
holes. This is helpful when only the outside nish of the model is important.
Keep Open Faces
This will ignore all manifold errors in the object. It can create issues
generating the Gcode as Cura does not know how to interpret the open
holes. This option should only be used if you are sure that the holes in the
mesh are intended. In general, you should not use this option.
44
Page 45
1.23. DUAL EXTRUSION
Extensive Stitching
This causes Cura to automatically add triangle meshes in an attempt to
x manifold errors. This algorithm will greatly increase Gcode generation
time and may end up adding in un-intended meshes. It is recommended
that you repair your model through MeshLab, FreeCAD or your preferred
CAD program before attempting this option.
1.23 Dual Extrusion
The LulzBot TAZ has the ability to add dual extrusion functionality with
the Dual Extruder tool head add-on. We only recommend the Dual
Extruder tool head for advanced users. Installation and operation of
the dual extruder will require you to ash your rmware, calibrate your
extruders, level two heads to a single plane, dene extruder osets, and
ne tune your slicing prole. This can be a little overwhelming for new
users. We recommended that you have a couple of months of single extruder
printing experience before making the switch.
Updating Firmware
In order to use the Dual Extruder you will need to update your rmware
to activate the second hot end.
• Power on your 3D printer and connect it to your computer through
USB.
• Select Machine > Machine Settings.
• In the top right-hand corner you will see a Change Tool Head button,
select this.
• Next you will need to select the proper hot end type. Please compare
photos with your existing tool head. Choose the correct hot end and
select Next.
• Select the photo that corresponds with your tool head and press Next.
45
Page 46
3D Printer Software
• The nal step will be flashing the firmware. Choose Flash the
firmware to be sure to update the printers rmware to the proper
settings. This must be done to allow your printer to operate properly.
• Once the progress bar has completed select OK > Next > Finish.
• You can verify this by looking at the LCD screen. You should now
see three temperature readings.
You can revert the rmware back to the stock conguration for your
LulzBot™3D printer by selecting Machine > Machine Settings > Change
Tool Head. Doing so will overwrite any of your current rmware settings.
Calibrating Extruders
Each individual extruder will have its own unique set of Esteps. To
determine this, you will need to tell the extruder to take in 100mm of
lament.
• Load the outer and inner calibrations squares into Cura
https://www.lulzbot.com/support/downloads
• Open the Printer Interface window and set temperatures for both
heads. Switch between hot ends by entering “T0” for the rear extruder
into the command line terminal. Press enter.
• Type “T1” for the front extruder into the command line terminal.
Press enter.
• Make two marks at 100mm and 120mm on the lament from the top
surface of each extruder.
• Once at the correct extrusion temperature type into the command
line “G92” and press enter. Then “G1 E100 F60” and press enter.
• Switch to the other tool head by entering “T0” for the rear or “T1”
for the front.
• Type into the command line “G92” and press enter.
• Type “G1 E100 F60” and press enter.
46
Page 47
1.23. DUAL EXTRUSION
• Measure the distance that the tool head over or under extruded. You
will need to adjust your Esteps by 8 up or down for each mm it under
or over extruded.
• Update your Esteps for the rear extruder and E1steps for the front
extruder through your LCD screen. Configuration > Advanced
Settings > E/E1 Steps > New Number. Push in on the knob to
exit out of the Esteps entry.
• Store your new Esteps Configuration > Store Memory.
Dening Second Extruder Oset
To get crisper looking prints, you will want to really dial in your osets.
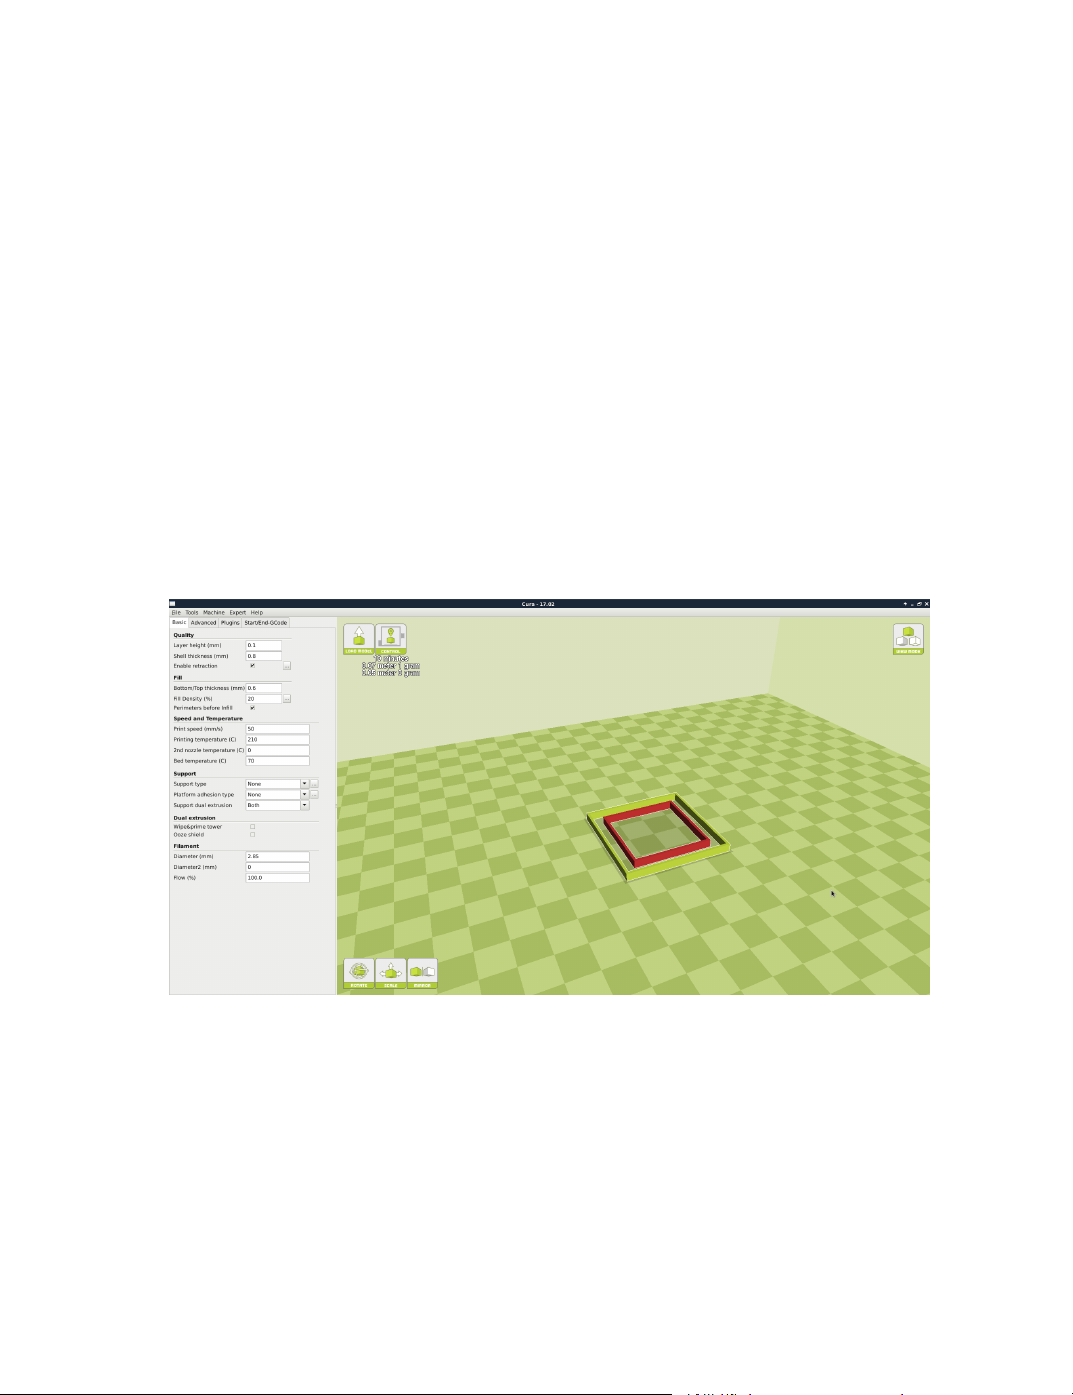
With the outer and inner square on your build platform, right click and
select Dual Extrusion Merge. The red square will be printed with your
front extruder, and the yellow square will be printed with the rear extruder.
After printing the squares, you will want to measure Top, Bottom, Left,
and Right gap. Enter these numbers into our oset calculator found here:
https://www.lulzbot.com/dual-extruder-calibration-calculator
This will produce new osets, that will need to be updated in the Machine
Settings menu. Repeat as many times as desired to truly ne tune the
oset.
47
Page 48
3D Printer Software
First Dual Print
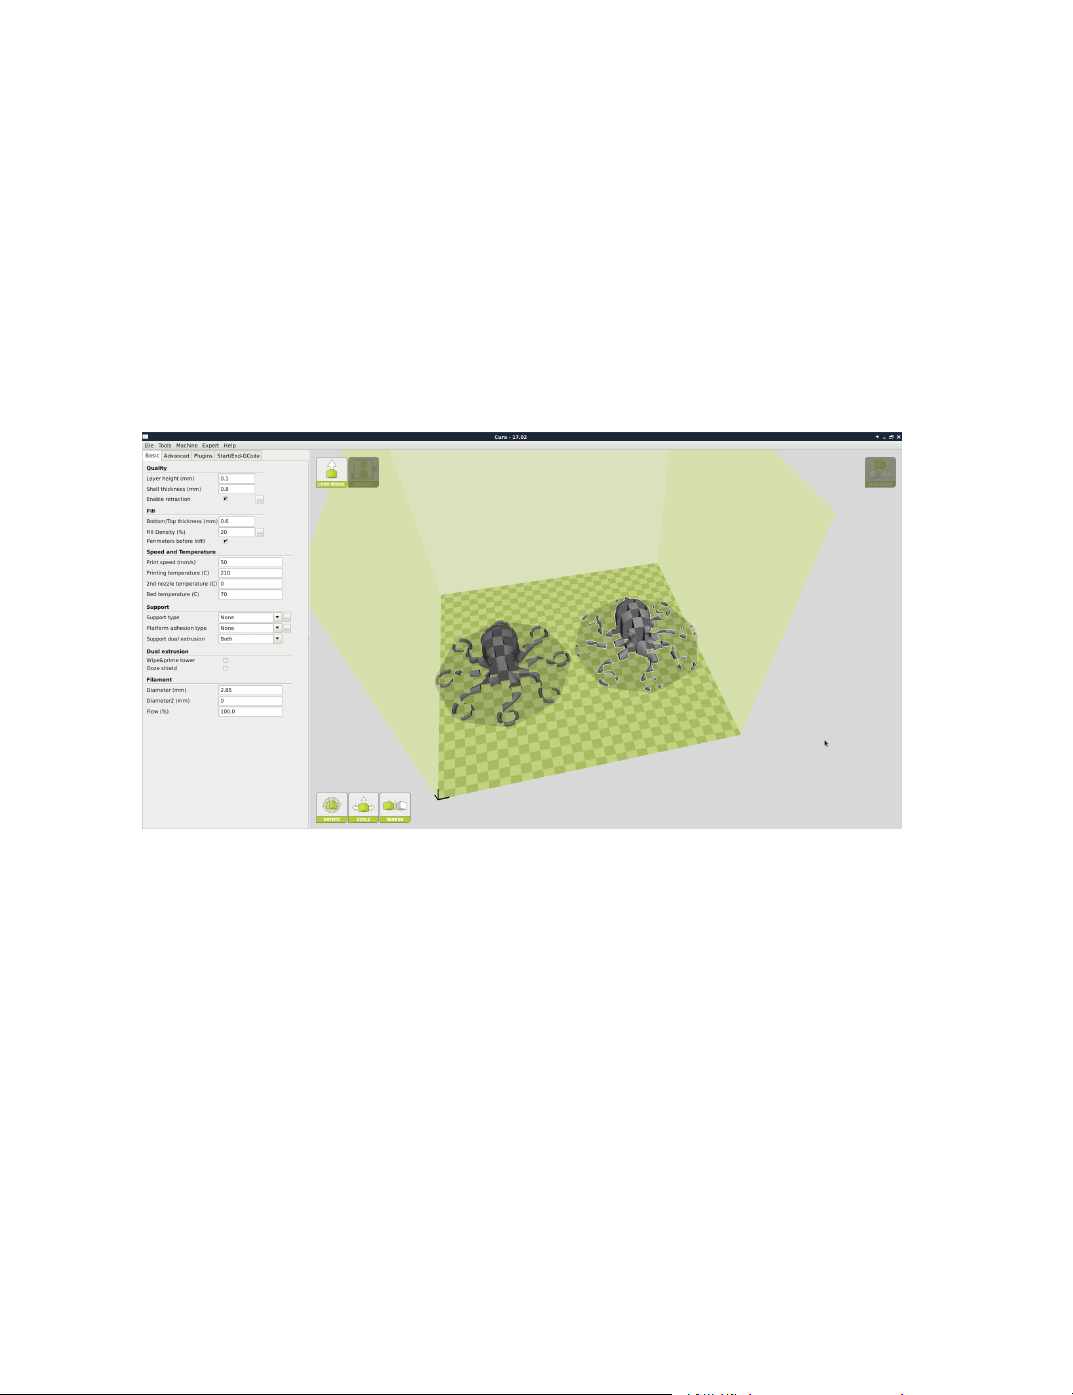
When you are ready to produce your rst dual extrusion print, you will
need to combine the two separate STL les. One STL le will be for each
print head. Left Click on whichever STL you would like printed with the
Rear Tool head. Then Right Click on whichever STL le you would
like printed with the Front Tool head and select dual extrusion merge.
You will now see a single model in two colors on the build plate. The red
section will be printed with the front extruder, while the green section will
be printed with the rear extruder.
Figure 1.19: Before Merge
48
Page 49
Setting Dual Temps
1.23. DUAL EXTRUSION
Figure 1.20: After Merge
After your object has been merged as intended, you will need to set the
individual temperatures for each print head. In order to switch between
which hot end you are heating, you will need to manually enter T0 to set
temps for the rear hot end, and T1 to set temps for the front hot end. The
Bed temp can be set from either T0 or T1. Once both print heads
and the print surface have reached the desired printing temperature select
Print.
49
Page 50
3D Printer Software
1.24 Printrun
Website: http://www.github.com/kliment/Printrun The host software,
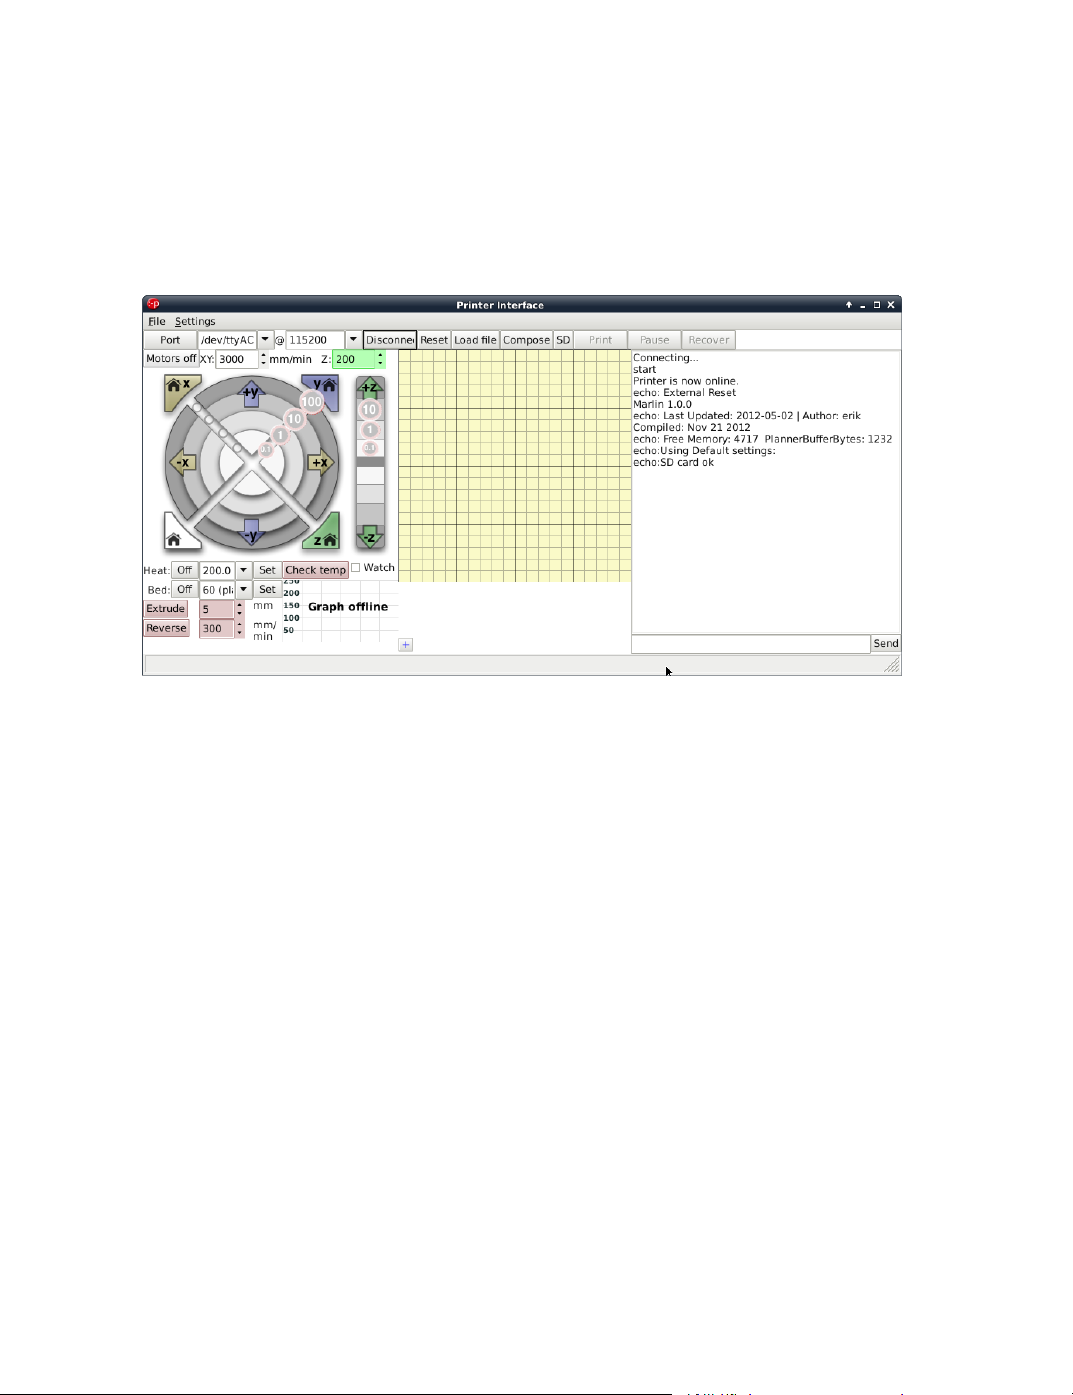
Printrun, can be used to start up and control your 3D printer (Figure 1.22,
page 52). The host controls include: setting the extruder and print surface
Figure 1.21: Printrun application for 3D printer control
temperatures, manual control of each axis, and manual extrusion. The host
is also where you can push print les (.gcode) to the 3D printer or load
print les from the SD card for printing out model designs.
Installing Printrun
Printrun contains several dierent applications that can be used to control
the LulzBot™TAZ 3D printer. It can be installed on Windows, Mac OSX
and Linux based computers. Pronterface is the graphical user interface
for Printrun. Pronsole allows printing from the command line, and
can be used for scripting and some automation. Plater allows you
to arrange and combine several STL les into one. More information
on the other programs within the Printrun package can be found at
https://github.com/kliment/Printrun. Printrun can be downloaded
from LulzBot.com/downloads. Download the version for your operating
system and extract. You will need an archive manager to extract the les.
50
Page 51
1.24. PRINTRUN
If you do not have one installed we recommend using 7-zip, which can be
downloaded for free at www.7-zip.org.
Windows Instructions
• Once downloaded, extract the dist folder to a location of your
choice. You can rename the dist folder if you like. Double click
pronterface.exe to run Pronterface.
Mac OSX Instructions
• Once downloaded, extract the dist folder to a location of your choice.
Once extracted, double click the pronterface-mac.app le to install.
Linux Instructions
Debian|Ubuntu
Recommended Installation
• We recommend using the stand-alone Printrun option found at
https://www.LulzBot.com/downloads. Once downloaded and extracted, navigate to the extracted directory. Install the dependencies
by issuing the following command in a terminal: sudo apt-get
install python-serial python-wxgtk2.8 python-pyglet. Once
the dependencies have been installed, run Pronterface by using the
following command in a terminal: python pronterface.py.
Installing from source
• Using Git, in a terminal issue the following command: git clone
https://github.com/kliment/printrun.git
• Once downloaded, change to the Printrun directory. You will need to
ensure that the following dependencies are met. They are listed in the
README.md le. You can use this command to install the dependencies: sudo apt-get install python-serial python-wxgtk2.8
python-pyglet python-tornado python-setuptools
51
Page 52
3D Printer Software
python-libxml2 python-gobject python-pip avahi-daemon
libavahi-compat-libdnssd1 followed by: pip install -r
requirements.txt To install in a terminal issue the following
command: sudo python setup.py install. Run Printrun by
issuing the following command: python pronterface.py
Fedora
• Use this command to install Printrun from the ocial sources: sudo
yum install printrun
Archlinux
• Use this command to install Printun from AUR: yaourt rintrun
1.25 Using Printrun
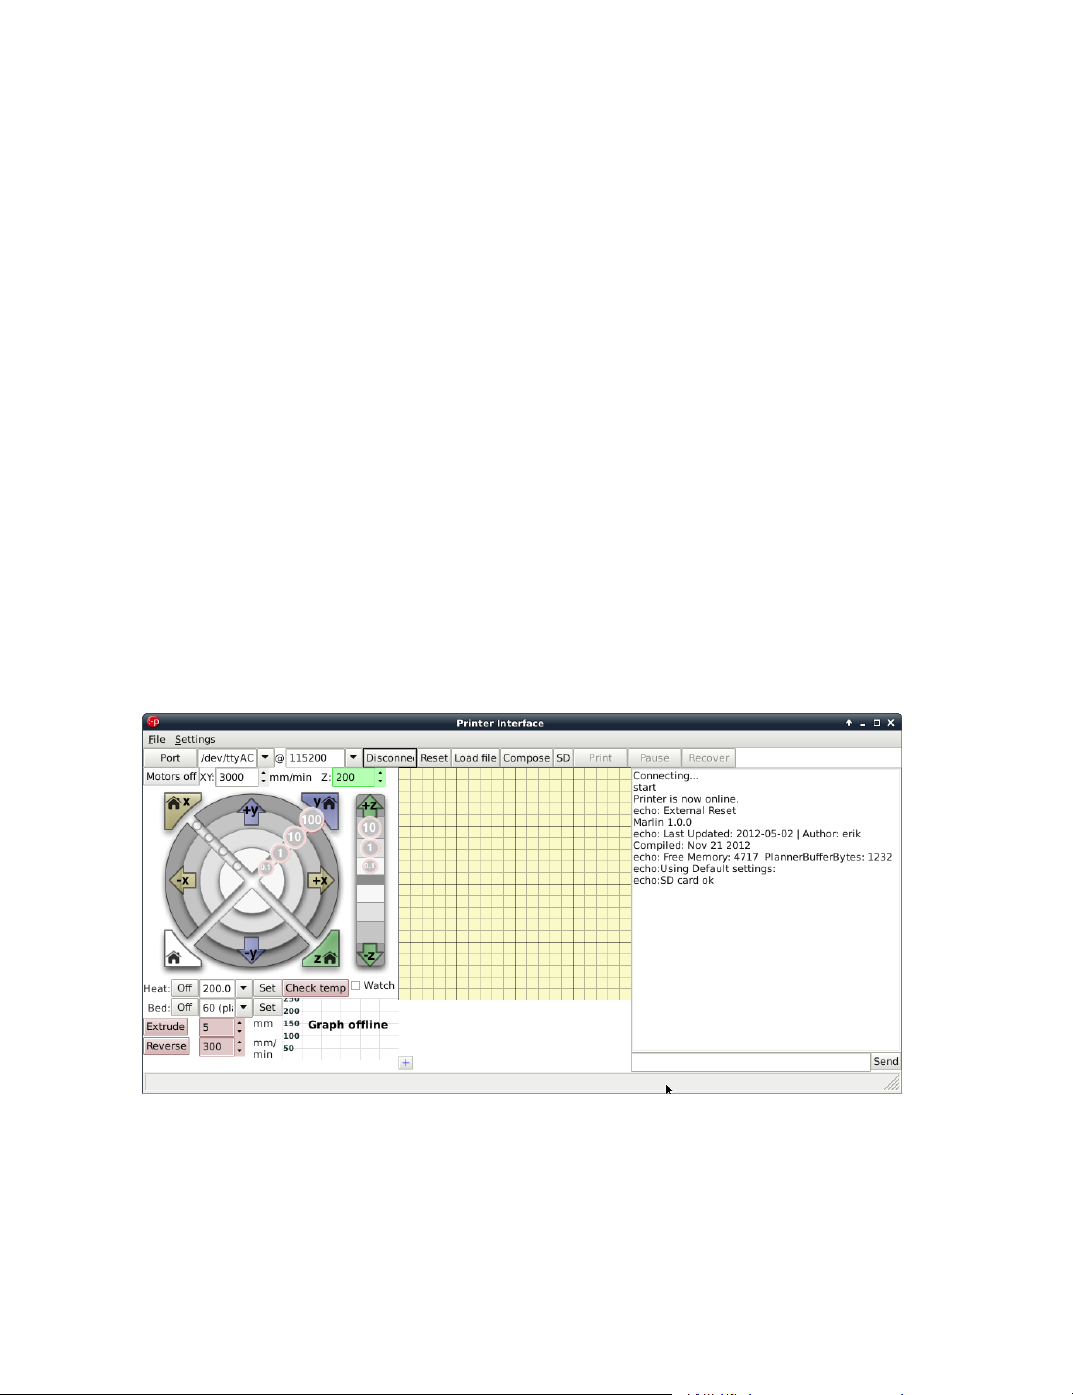
Figure 1.22: Printrun
52
Page 53
1.25. USING PRINTRUN
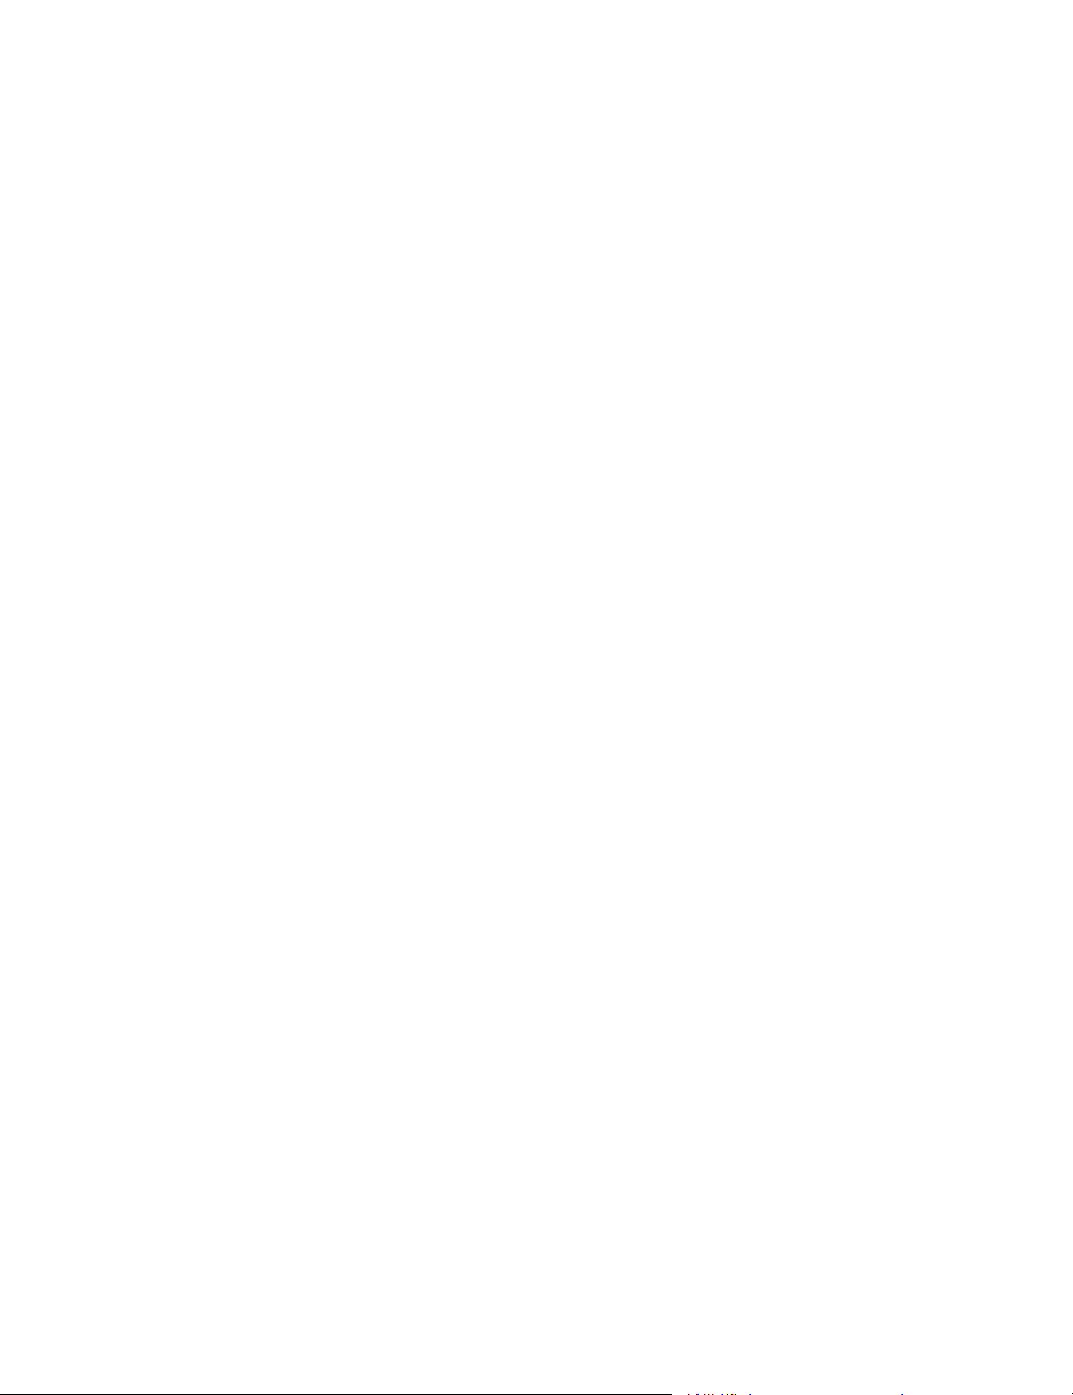
Printrun is used to control the printer from a computer. It is divided into
4 main parts: The buttons over the top are used to connect to the printer,
load les and start & stop prints.
The movement controls are on the left hand side, with the G-code
preview window in the center and the Log window and Terminal command
entry box on the right hand side (Figure 1.22, page 52).
Connecting to the your 3D Printer
To start up the printer, rst you will need to connect to the printer with
Printrun. Make sure you have connected the USB cable from your PC
to the printer before launching Printrun. If not, close Printrun, connect
the USB cable, and relaunch Printrun. To connect to the printer, select
the correct port by using the drop down arrow and selecting the active
port, generally /dev/ttyACM0). On other operating systems the port may
be named such as COM1 or tty.usbserial-USB-ID. The Port button will
refresh the Port listing. Once selected choose the default 115200 buad rate
and press Connect. Pronterface will open a connection to the printer and
display rmware information in the Log window.
In the text output window you will see multiple return lines. If you see
Printer is now online you have successfully connected to the printer.
The printer control buttons on the left will also darken and become clickable after connecting. If nothing is displayed in the Log window verify you
have the correct port and connection speed selected. When you need to
disconnect the printer simply press the Disconnect button.
53
Page 54
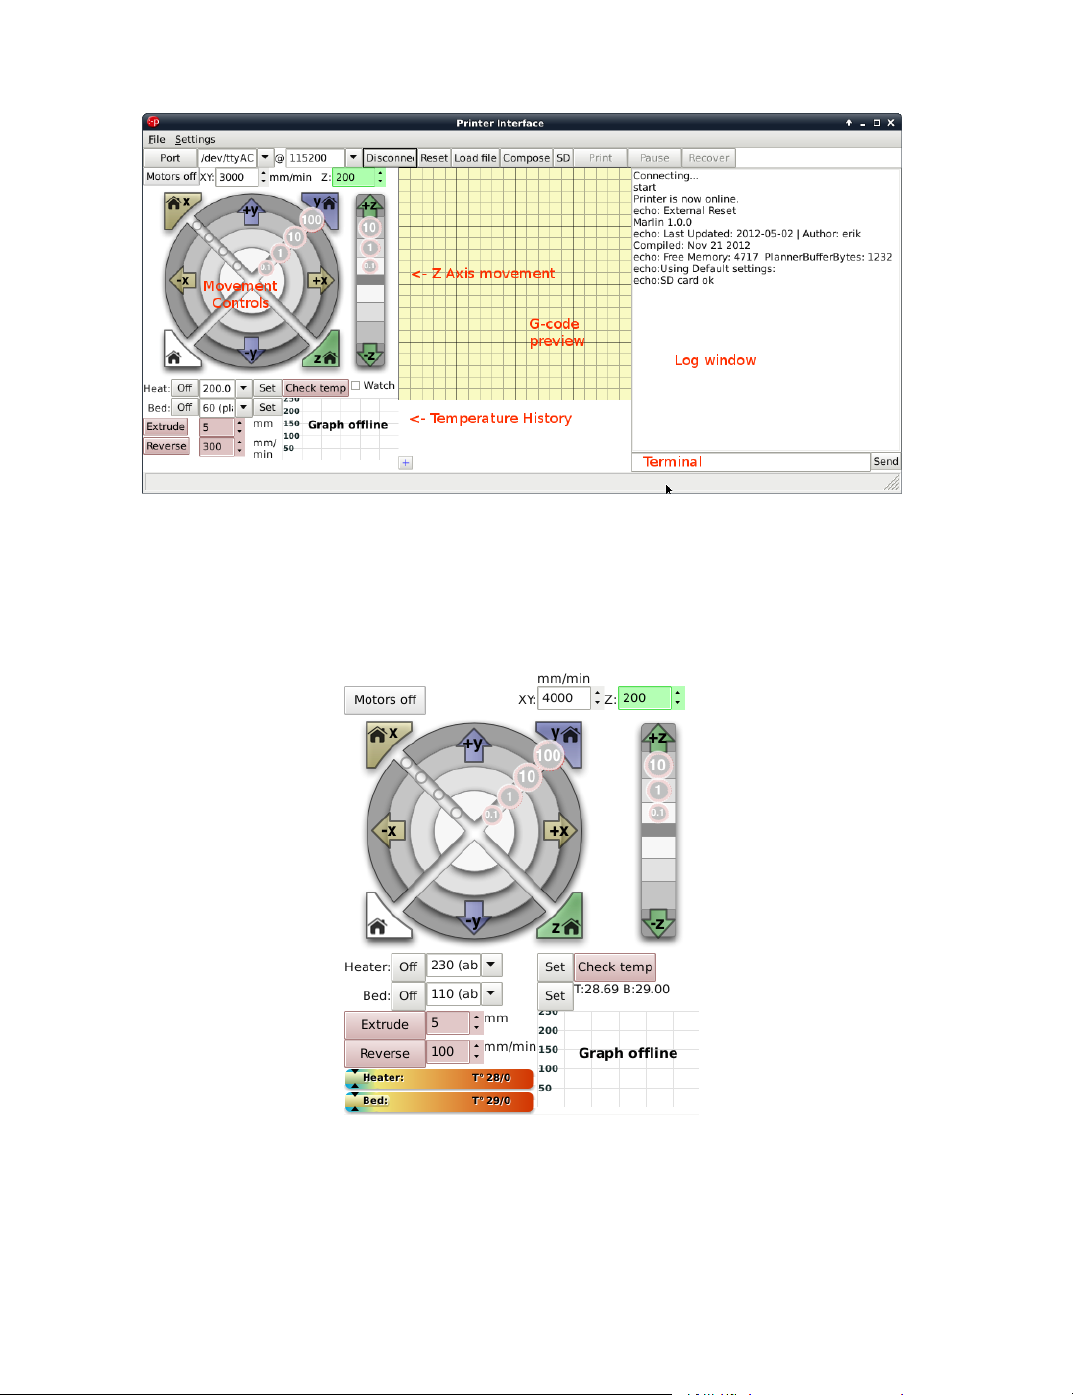
Movement
3D Printer Software
Figure 1.23: Printrun Functions
Figure 1.24: Movement Controls
54
Page 55
1.25. USING PRINTRUN
Motors o
Your 3D printer can be moved on all three axes independently. If you would
like to do so by hand, use the Motors off button to unlock all the stepper
motors. Once unlocked they can be moved by hand. Keep in mind that
there is no positional feedback, so if you move an axis you will need to
re-home in order to re-establish the hot end’s position.
mm/min XY:/ Z:
These settings control the manual jog speeds when driven with Pronterface.
Use caution when changing these gures. Moving the axes too fast can
cause the printer to miss steps. If that occurs with the Z axis, it can
potentially cause the Z axis to become out of square.
Homing
Caution: when homing, the axis will continue to move in the negative
direction until the end stop switch is activated. If the printer is ever
transported make sure the end stop switches are clear before resuming
printing. If an axis has missed an end stop and is continuing to try to
move in the negative direction, immediately turn the power switch to the
o position.
Each axes can be homed either individually or together. Press the Home
X button to move the X axis to the left until it activates the end stop. Once
the X axis end stop is activated, the X axis carriage will ‘bounce’. It will
move over and move back to the home position more slowly. Press the Home
Y button to home the Y axis. The Y axis platform will move away from
you towards the rear of the printer.
X/Y/Z Axes Movement Controls
Prior to moving the X, Y, or Z axis, make sure that you home each axis.
The X, Y and Z axes can be moved utilizing the circular movement controls.
Each axis can be moved in either ne moves or large moves, ranging from
0.1mm to 100mm. For example, to move the Y Axis towards you, move
your mouse to the +y section until both the +y and the 100 are highlighted
then select that ring section. To move the Y axis away from you, move
your mouse to the -y section until both the -y and the 100 are highlighted
55
Page 56
3D Printer Software
then select that ring section. The X axis can be moved in a similar fashion.
The Z axis movement control operates similarly, but the movement scale
is dierent. The Z axis will move in 0.1mm, 1mm and 10mm increments.
The top half of the movement bar will move the Z axis up, by the selected
units, while the lower half will move the Z axis down, by the selected units.
1.26 CAD and 3D Modeling Software
LulzBot is not distributing a CAD or 3D modeling software package. However, multiple free/libre software packages are available. Other common
non-free CAD and 3D modeling software are also capable of exporting the
required .STL les.
On some CAD and 3D modeling software you will need to select
millimeters as the output unit. If possible it is best to build your 3D design
in metric units rather than imperial units. Slic3r requires .STL les sized
in millimeters. If an .STL with inches as units is loaded into the Slic3r, the
model will be scaled much smaller than expected. You can scale the model
by 2540% to compensate. The software listed below outputs millimeters as
the unit by default.
FreeCAD
Website: http://free-cad.sourceforge.net
Although still in development, FreeCAD is a great free/libre CAD
application. Containing a full GUI for building CAD models, FreeCAD
is capable of creating simple to complex designs. STL les can also easily
be exported for use with 3D printing. FreeCAD is available for GNU/Linux,
Windows, and Mac. The latest development version is recommended.
OpenSCAD
Website: http://openscad.org
OpenSCAD is another free/libre CAD software; however, dierent than
FreeCAD, it is script based. Rather than using a GUI to generate CAD
designs, OpenSCAD CAD designs are created using script based renderings.
Users with programming experience would nd this very useful. Also,
OpenSCAD uses a simple script language that is easy for users with little
56
Page 57
1.27. ALTERNATIVE PRINTER HOST SOFTWARE
or no programming experience to learn.
Blender
Website: http://blender.org
The most widely used free/libre 3D modeling software, Blender is well
documented with tutorials available on the Blender.org website as well as
found online.
Shapesmith
Website: http://shapesmith.net
Shapesmith is a web-based 3D modeling software. This means there is
no required software to get started designing models. Shapesmith is also a
great choice for anyone starting out in CAD/ 3D modeling.
1.27 Alternative Printer Host Software
OctoPrint
Website: http://octoprint.org/
Octoprint is a printer host that uses a web-based interface to access
and control your 3D printer. Added web-cam functionality allows for timelapse videos and a live stream. Octoprint will run on Windows, Apple, and
Linux based computers and can even run well on a Beagle Bone Black or
a RaspberryPi (inexpensive business-card sized computers).
BotQueue
Website: https://www.botqueue.com/
BotQueue works well for those users wanting to have a web-based
multiple 3D printer operation running o a queuing system.
MatterControl
Website: http://www.mattercontrol.com/
57
Page 58
3D Printer Software
MatterControl is another printer host that currently runs on Windows
and Apple computers. It features 2D and 3D model viewing, a print queue,
and print le organization and searching.
58
Page 59
Slic3r
Page 60
Slic3r
2.1 Introduction
Overview
Slic3r is a tool which translates digital 3D models into instructions that
are understood by a 3D printer. It slices the model into horizontal layers
and generates suitable paths to ll them.
Slic3r is already bundled with the many of the most well-known host
software packages: Pronterface, Repetier-Host, ReplicatorG, and can be
used as a standalone program.
This manual will provide guidance on how to install, congure and
utilize Slic3r in order to produce excellent prints.
This portion of the manual is derived from the complete Slic3r manual.
It has been customized for TAZ users. The original unabridged version
can be found at manual.slic3r.org. Due to the introduction of Cura
LulzBot™Edition, the recommended printer host and slicer, this abriged
Slic3r manual may not be current.
Goals & Philosophy
Slic3r is an original project started in 2011 by Alessandro Ranellucci (aka.
Sound), who used his considerable knowledge of the Perl language to create
a fast and easy to use application. Readability and maintainability of the
code are among the design goals.
The program is under constant renement, from Alessandro and the
other contributors to the project, with new features and bug xes being
released on a regular basis.
Donating
Slic3r started as a one-man job, developed solely by Alessandro in his
spare time, and as a freelance developer this has a direct cost for him.
By generously releasing Slic3r to the public as open source software, under
the GPL license, he has enabled many to benet from his work.
The opportunity to say thank you via a donation exists. More details
can be found at: http://slic3r.org/donations.
60
Page 61
2.2. GETTING SLIC3R
2.2 Getting Slic3r
Slic3r is Free Software, and is licensed under the GNU Aero General Public
License, version 3.
Downloading
From LulzBot.com
The Slic3r version that has been tested for the TAZ printer
can be downloaded from the LulzBot.com downloads page:
https://www.lulzbot.com/Slic3r.
Pre-compiled packages are available for Windows, Mac OS X and Linux.
Windows and Linux users can choose between 32 and 64 bit versions to
match their system.
Slic3r
Slic3r can be downloaded directly from: http://slic3r.org/download.
Pre-compiled packages are available for Windows, Mac OS X and Linux.
Windows and Linux users can choose between 32 and 64 bit versions to
match their system.
Manual
The latest version of full Slic3r manual, with LATEX source code, can be
found at: https://github.com/alexrj/Slic3r-Manual
Source
The source code is available via GitHub: https://github.com/alexrj/Slic3r.
For more details on building from source see §2.2 below.
Installing
Linux
Extract the archive to a folder of your choosing. Either:
61
Page 62
Slic3r
• Start Slic3r directly by running the Slic3r executable, found in the
bin directory, or
• Install Slic3r by running the do-install executable, also found in the
bin folder.
The archive le may then be deleted.
Windows
Unzip the downloaded zip le to a folder of your choosing, there is no
installer script. The resulting folder contains two executables:
• slic3r.exe - starts the GUI version.
• slic3r-console.exe - can be used from the command line.
The zip le may then be deleted.
Mac OS X
Double-click the downloaded dmg le, an instance of Finder should open
together with an icon of the Slic3r program. Navigate to the Applications
directory and drag and drop the Slic3r icon into it. The dmg le may then
be deleted.
Building from source
For those wishing to live on the cutting edge, Slic3r can
be compiled from the latest source les found on GitHub
https://github.com/alexrj/Slic3r.
Up-to-date instructions for compiling and running from source can be
found on the Slic3r wiki.
2.3 First Print
Calibration
Your LulzBot™TAZ 3D printer was calibrated at the factory prior to
packing. TAZ users do not need to calibrate their printers.
62
Page 63
2.3. FIRST PRINT
If you are just beginning with 3D printing or Slic3r, LulzBot™recommends starting with our pre-set Slic3r proles. You can nd the TAZ Slic3r
proles at https://www.lulzbot.com/Slic3r. For information on loading
and export Slic3r proles please see page 117. Note that the pre-set proles
will only work correctly when Slic3r is in Expert mode.
The pre-set proles will give you Slic3r settings that will work great on
most designs. The Slic3r manual can be used as a reference in building
knowledge of Slic3r settings while using the pre-set proles. Once you have
a number of prints completed you can use the Slic3r manual as a reference
to make small adjustments to the pre-set proles or begin creating your
own proles.
63
Page 64
Slic3r
Conguration Wizard
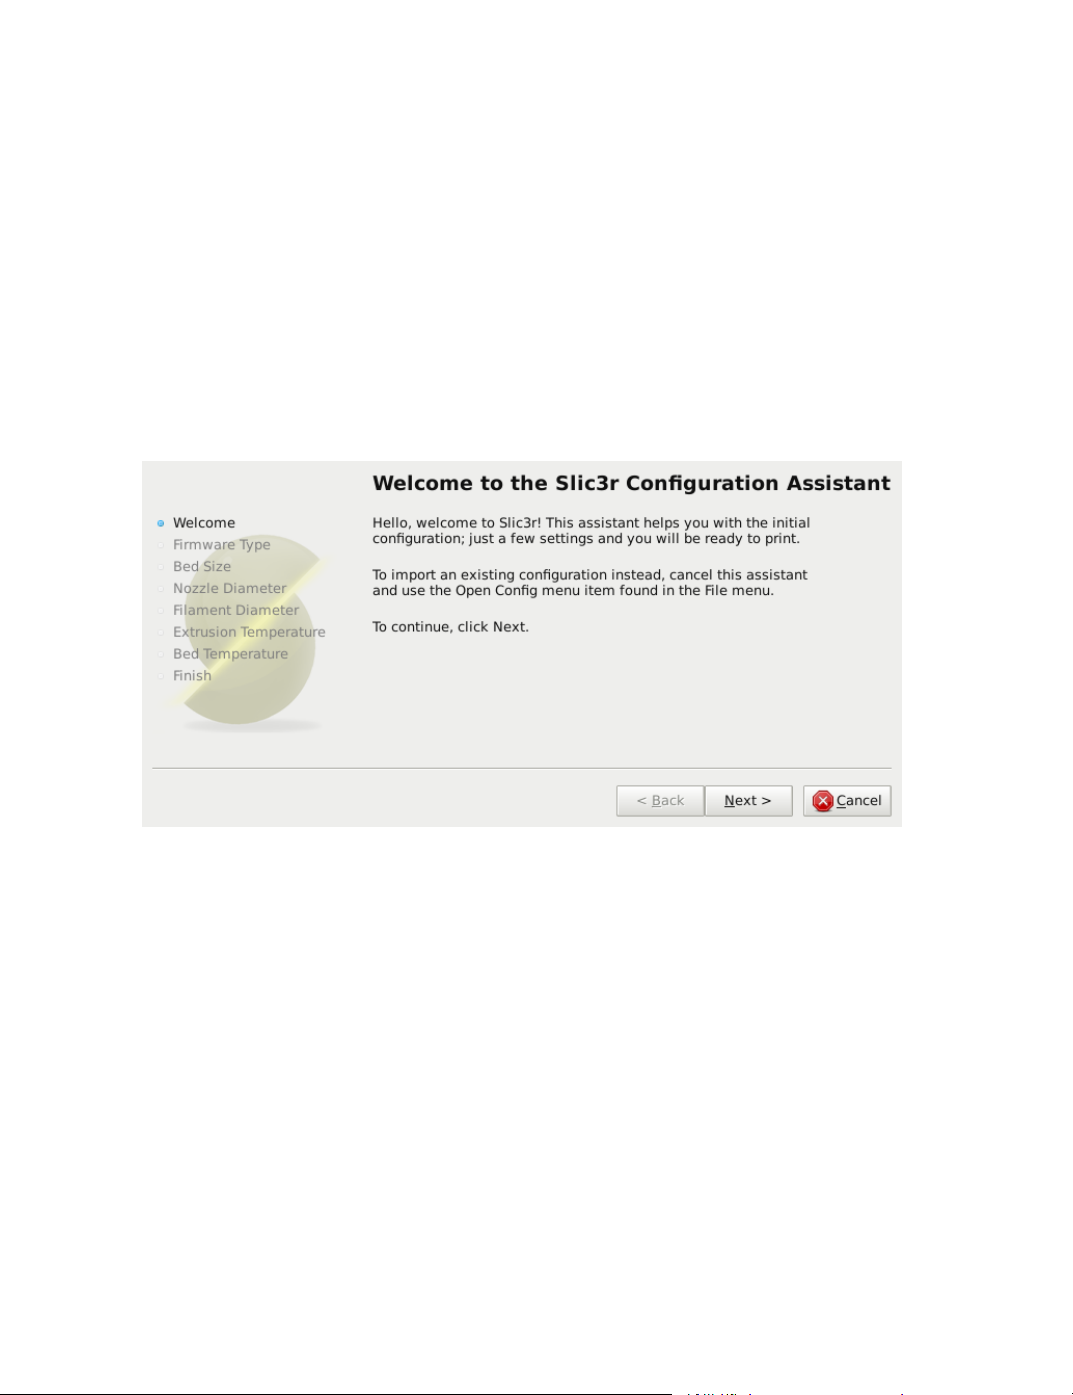
Slic3r has two features to aid newcomers: the conguration wizard, and
simple mode.
Sometimes it is nice to have a helping hand when starting out with new
software. The conguration wizard asks a series of questions and creates a
new conguration for Slic3r.
When using the pre-set TAZ Slic3r proles you do not need to complete
the Conguration Wizard. The Conguration Wizard can be later accessed
from the top menu once you are ready to start creating your own Slic3r
proles.
Figure 2.1: Conguration Wizard: Welcome Screen
64
Page 65
2.3. FIRST PRINT
1. Firmware Type
The gcode produced by Slic3r is tailored to particular types of rmware.
The rst step prompts for the rmware that the printer uses. For the TAZ
printer select RepRap (Marlin/Sprinter)
Figure 2.2: Conguration Wizard: Firmware Type
65
Page 66
Slic3r
2. Bed Size
This setting denes the maximum distance the extruder may travel along
the X and Y axis. The dimensions for the TAZ print surface are X: 298
and Y: 275.
Be sure to measure from the lower left corner where the extruder nozzle
rests when are the home position to the maximum distance the nozzle can
travel in each direction. Take into account that the X carriage may touch
the frame before the nozzle reaches it’s full distance, this will depend on
the printer make and model.
Figure 2.3: Conguration Wizard: Bed Size
66
Page 67
2.3. FIRST PRINT
3. Nozzle Diameter
The diameter of the hot-end nozzle is usually clearly displayed either in the
description of the hot-end, or in the associated documentation, when the
hot-end is purchased. The nozzle sizes available for the TAZ hot end are
0.35mm and 0.50mm.
If the nozzle was home-made, or came from a source without a diameter
given, then carefully measure the aperture as accurately as possible. One
way of determining nozzle size is to very slowly (1mm/s) extrude some
lament into free air and measure the thickness of the resulting extrusion1.
This has the benet of taking die swell into account, and consequently may
be a useful thing to do even if the diameter is known.
Figure 2.4: Conguration Wizard: Nozzle Diameter
1
http://forums.reprap.org/read.php?1,113374,113953
67
Page 68
Slic3r
4. Filament Diameter
For Slic3r to produce accurate results it must know as accurately as possible
how much material is pushed through the extruder. Therefore it is vital to
give it as precise a value as possible for the lament diameter.
Although the lament used in FDM printers is sold as being either
3mm or 1.75mm this is only a general guide. The diameter can vary
between manufacturers and even between batches. Therefore it is highly
recommended to take multiple measurements from along a length of the
lament and use the average. For example, measurements of 2.89, 2.88,
2.90 and 2.91 would yield an average of 2.895, and so this would be used.
Figure 2.5: Conguration Wizard: Filament Diameter
68
Page 69
2.3. FIRST PRINT
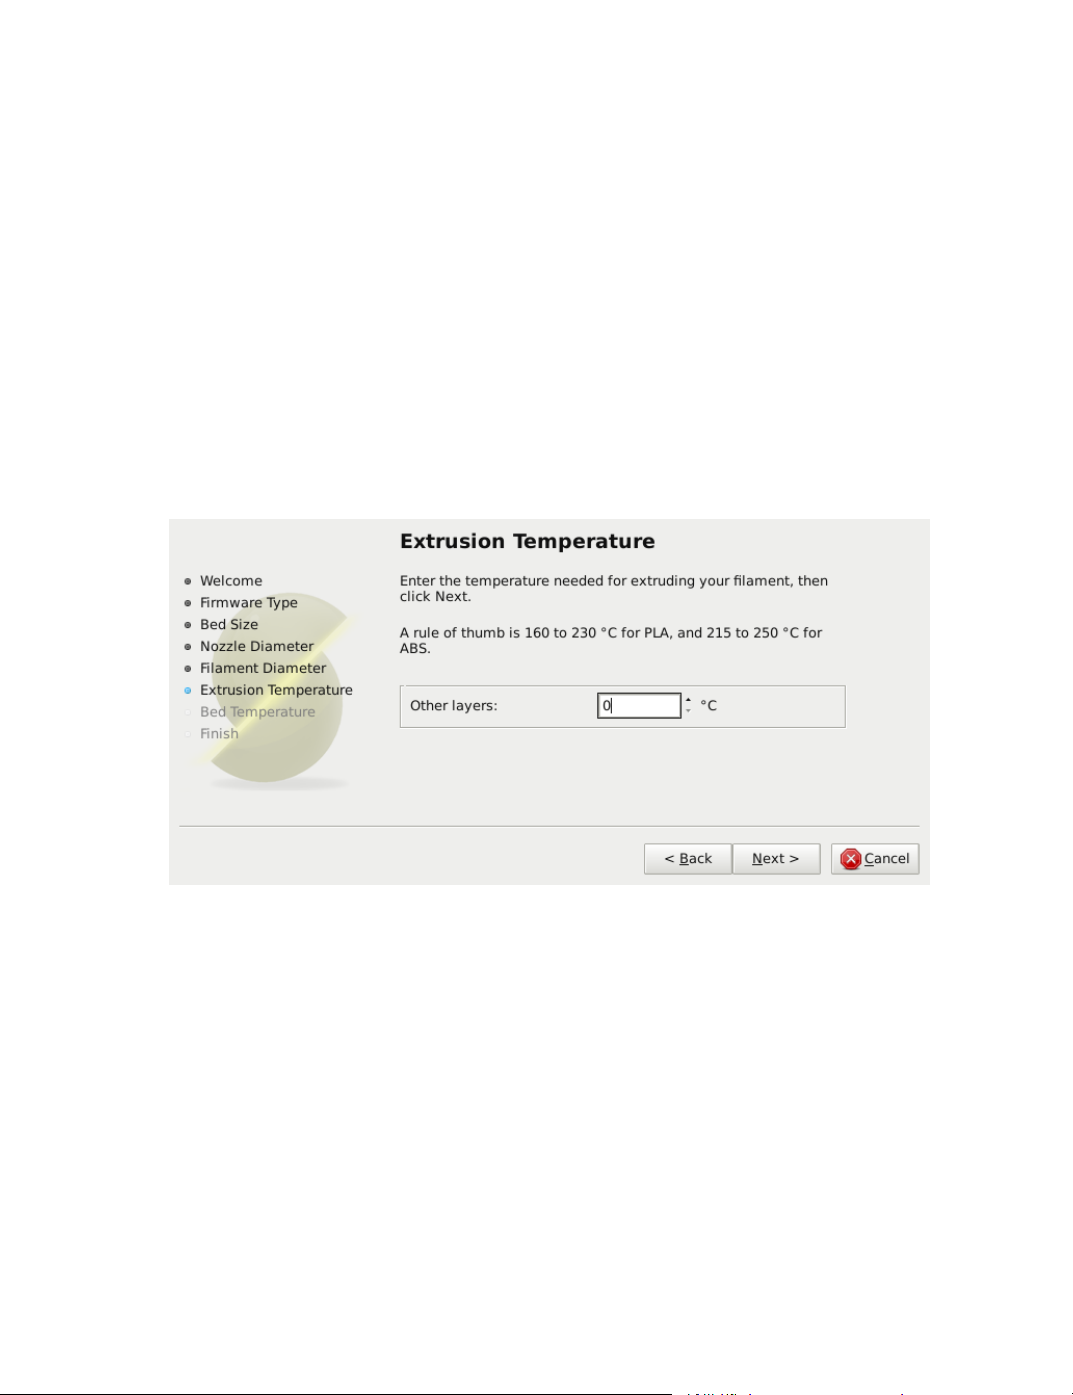
5. Extrusion Temperature
The extrusion temperature will depend on the material, and most can
operate over a range of temperatures. The supplier should provide guidance
as to which temperatures are suitable. A very general rule of thumb is that
PLA lies between 160°C and 230°C, and ABS lies between 220°C and 240°C.
More exotic materials will have a dierent range.
This is one parameter which you will want to ne tune when you start
producing prints. The optimal temperature can vary even between colors of
the same material. Another factor which may aect the chosen temperature
is how fast the extrusion is, where generally faster extrusion runs hotter.
Note: One may choose to control the extruder temperature manually
from the printer controller. In this case the temperature can be set to zero.
Figure 2.6: Conguration Wizard: Extrusion Temperature
69
Page 70
Slic3r
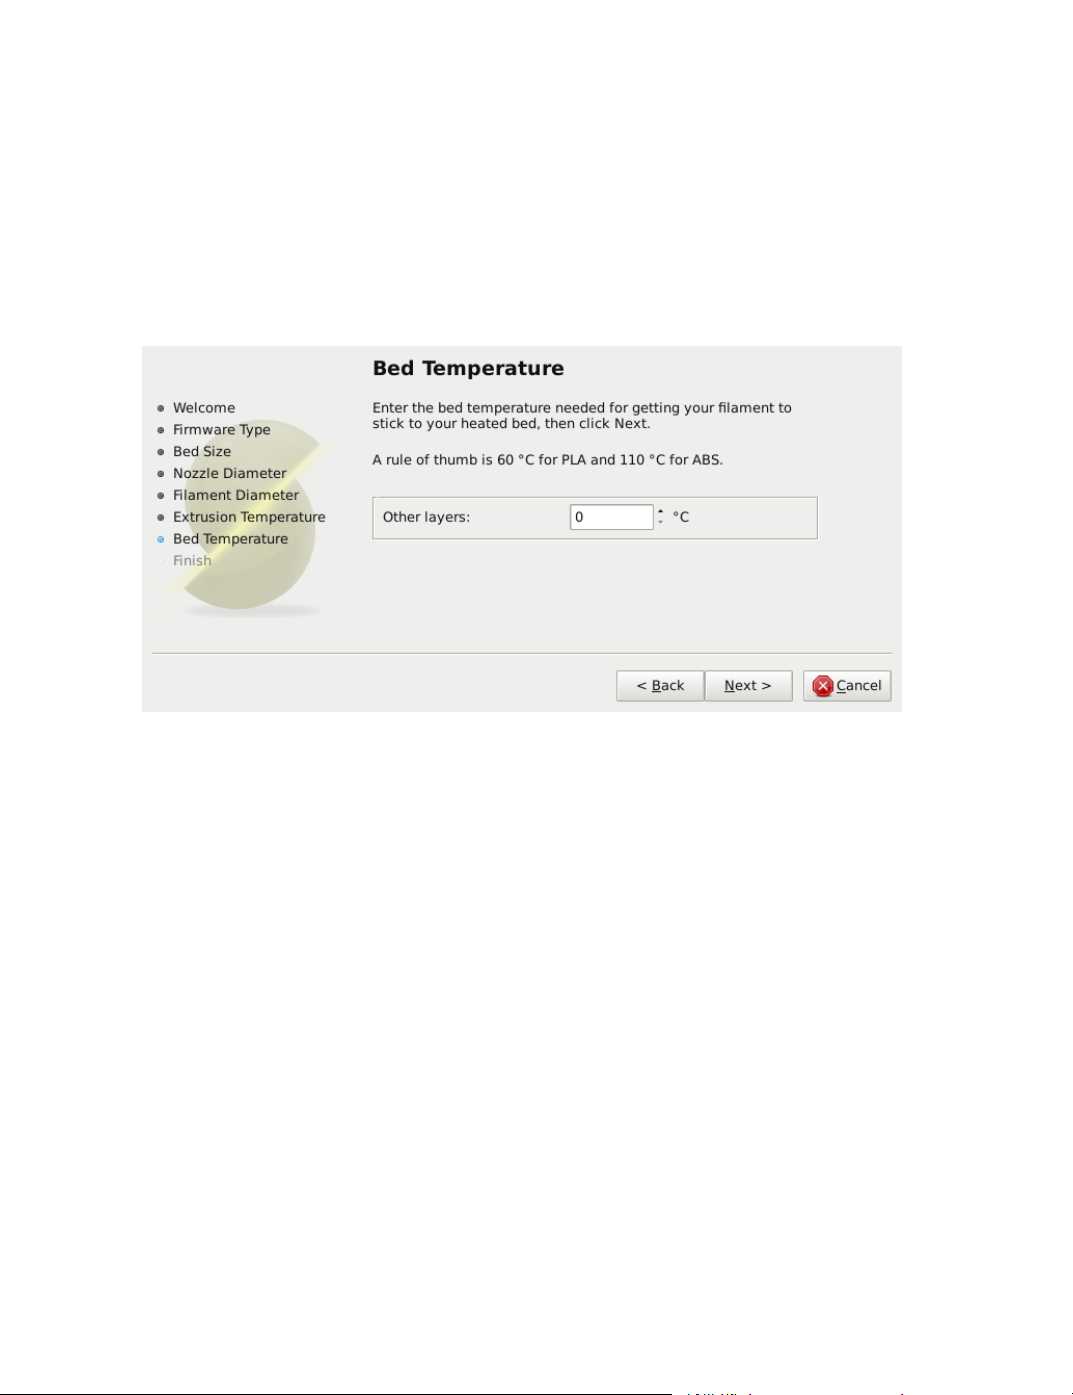
6. Bed Temperature
If the printer has a heated bed then this parameter may be set. As with
the extruder temperature, the value will depend on the material used. A
rule of thumb is that PLA requires 35°C - 60°C and ABS requires 85°C.
Note: One may choose to control the bed temperature manually from
the printer controller. In this case the temperature can be set to zero.
Figure 2.7: Conguration Wizard: Bed Temperature
70
Page 71
2.3. FIRST PRINT
At this stage the wizard is complete and the basic conguration is
dened.
Figure 2.8: Conguration Wizard: End
71
Page 72
Slic3r
The Important First Layer
Before delving into producing the rst print it is worthwhile taking a little
detour to talk about the importance of getting the rst layer right. As
many have found through trial and error, if the rst layer is not the best it
can be then it can lead to complete failure, parts detaching, and warping.
There are several techniques and recommendations one can heed in order
to minimise the chance of this happening.
Level bed. Having a level bed is critical. If the distance between the nozzle
tip and the bed deviates by even a small amount it can result in either the
material not lying down on the bed (because the nozzle is too close and
scrapes the bed instead), or the material lying too high from the bed and
not adhering correctly.
Higher temperature. The extruder hot-end and bed, if it is heated, can be
made hotter for the rst layer, thus decreasing the viscosity of the material
being printed. As a rule of thumb, an additonal 5° is recommended.
Lower speeds. Slowing down the extruder for the rst layer reduces the
forces applied to the molten material as it emerges, reducing the chances
of it being stretched too much and not adhering correctly. 30% or 50% of
the normal speed is recommended.
Correctly calibrated extrusion rates. If too much material is laid down
then the nozzle may drag through it on the second pass, causing it to lift
o the bed (particularly if the material has cooled). Too little material
may result in the rst layer coming loose later in the print, leading either
to detached objects or warping. For these reasons it is important to have
a well-calibrated extrusion rate as recommended in §2.3).
First layer height. A thicker layer height will provide more ow, and
consequently more heat, making the extrusion adhere to the bed more. It
also gives the benet of giving more tolerance for the levelness of the bed.
It is recommended to raise the rst layer height to match the diameter of
the nozzle, e.g. a rst layer height of 0.35mm for a 0.35mm nozzle. Note:
The rst layer height is set this way automatically in simple mode.
72
Page 73
2.3. FIRST PRINT
Fatter extrusion width. The more material touching the bed, the better
the object will adhere to it, and this can be achieved by increasing the
extrusion width of the rst layer, either by a percentage or a xed amount.
Any spaces between the extrusions are adjusted accordingly.
A value of approximately 200% is usually recommended, but note that
the value is calculated from the layer height and so the value should only
be set if the layer height is the highest possible. For example, if the layer
height is 0.1mm, and the extrusion width is set to 200%, then the actual
extruded width will only be 0.2mm, which is smaller than the nozzle. This
would cause poor ow and lead to a failed print. It is therefore highly
recommended to combine the high rst layer height technique recommended
above with this one. Setting the rst layer height to 0.35mm and the rst
extrusion width to 200% would result in a nice fat extrusion 0.65mm wide.
Bed material. Many options exist for the material to use for the bed, and
preparing the right surface can vastly improve rst layer adhesion.
PLA is more forgiving and works well on PEI, PET, Kapton, or blue
painters tape.
ABS usually needs more cajoling. While it’s generally preferred to print
directly on the PEI surface, a watered-down PVA or white school-glue
solution can help prints adhere to the bed and is preferred. Never use
anything with acetone on the PEI print surface as it can degrade the PEI
material.
No cooling. Directly related with the above, it makes no sense to increase
the temperature of the rst layer and still have a fan or other cooling
mechanism at work. Keeping the fan turned o for the rst few layers is
generally recommended.
73
Page 74
Slic3r
Working with Models
Yet another step lies between now and the rst print - a model has to be
obtained and then sliced.
Model Formats
Slic3r accepts the following le types.
• STereoLithography (STL) les can come from a wide variety of
sources and are now a de facto standard in 3D printing. The les
simply describe the surface geometry of a 3D object without any
additional information (such as color or material), and it is this
simplicity that has probably made the format ubiquitous.
• Wavefront OBJ les are an open format originally used in an ani-
mation application from Wavefront Technologies, but has since been
adopted by the wider 3D modelling community. It is similar to the
STL format.
• Additive Manufacturing File Format (AMF) was developed in re-
sponse to the limited nature of the STL format. In addition to
describing the geometry of the 3D model it can also describe colors
and materials, as well as more complex attributes, such as gradient
mixes and multiple object arrangements (constellations). Whilst the
format is deemed a standard it has yet to be widely adopted in the
3D maker community.
Finding Models
The 3D model les may come from an online repository, such as Thingiverse2or GrabCAD3, or be created from a CAD program, such as FreeCAD4,
Sketchup5, or OpenSCAD6, or an online CAD tool such as Shapesmith7.
2
http://www.thingiverse.com
3
http://grabcad.com
4
http://sourceforge.net/projects/free-cad
5
http://www.sketchup.com
6
http://www.openscad.org
7
http://shapesmith.net
74
Page 75
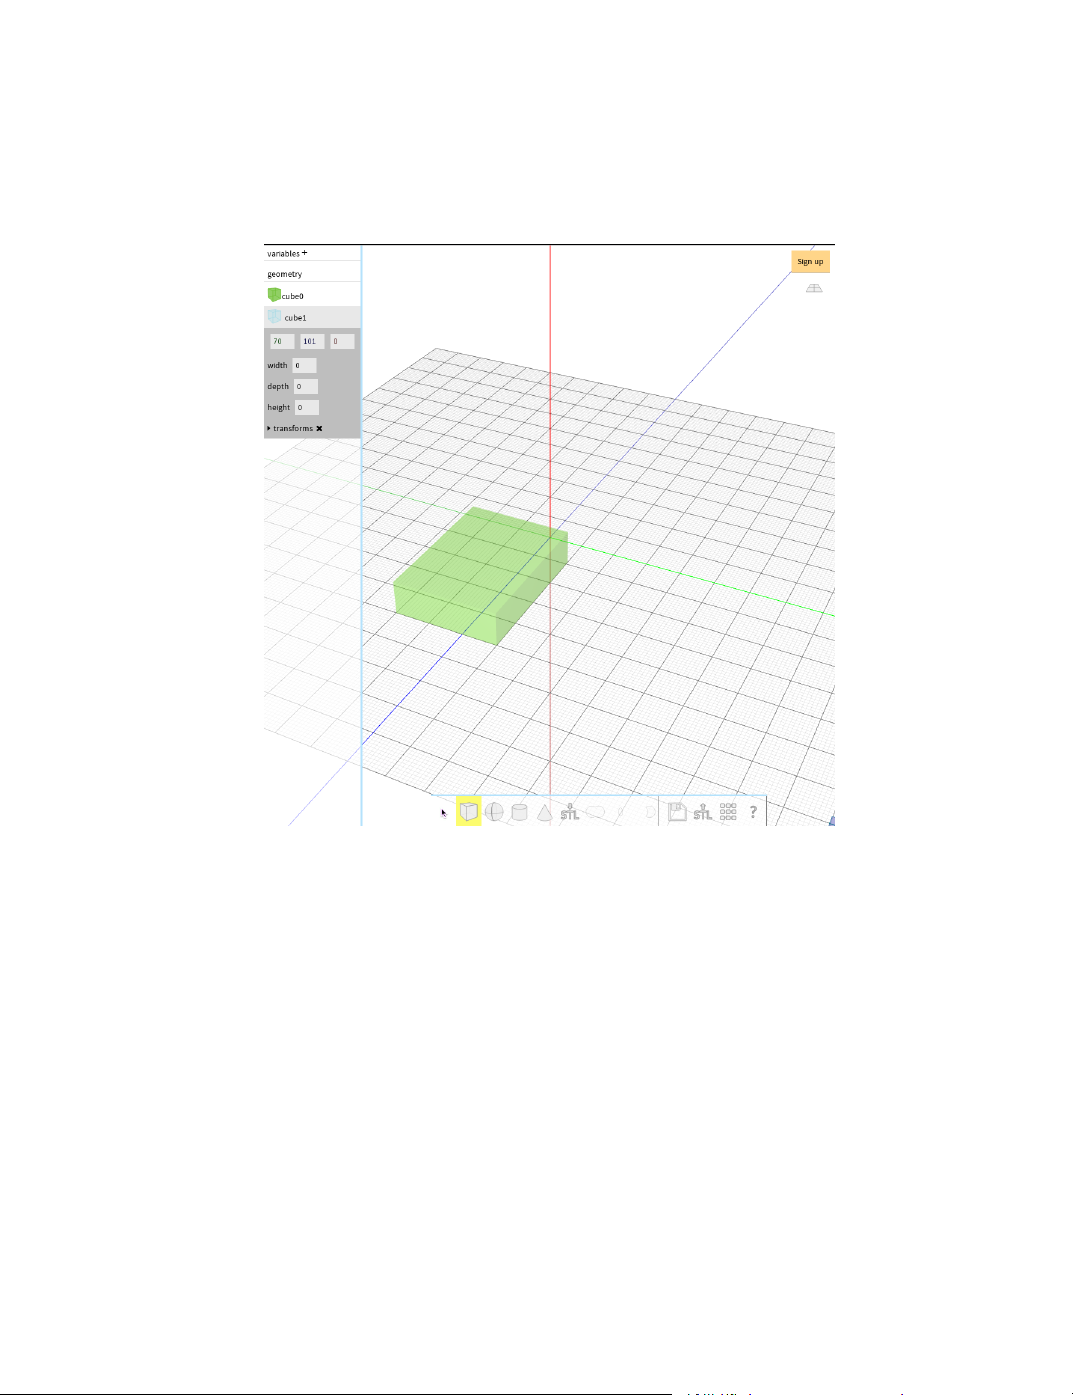
2.3. FIRST PRINT
You may wish to view the les before slicing and there are many free
applications available, one of which is Meshlab8- a comprehensive tool for
viewing and working with 3D les.
Figure 2.9: Shapesmith online CAD tool.
Working with Plater
Slic3r has a tool, called Plater, which allows one or more models to be
loaded and arranged before being sliced.
8
http://www.meshlab.org
75
Page 76
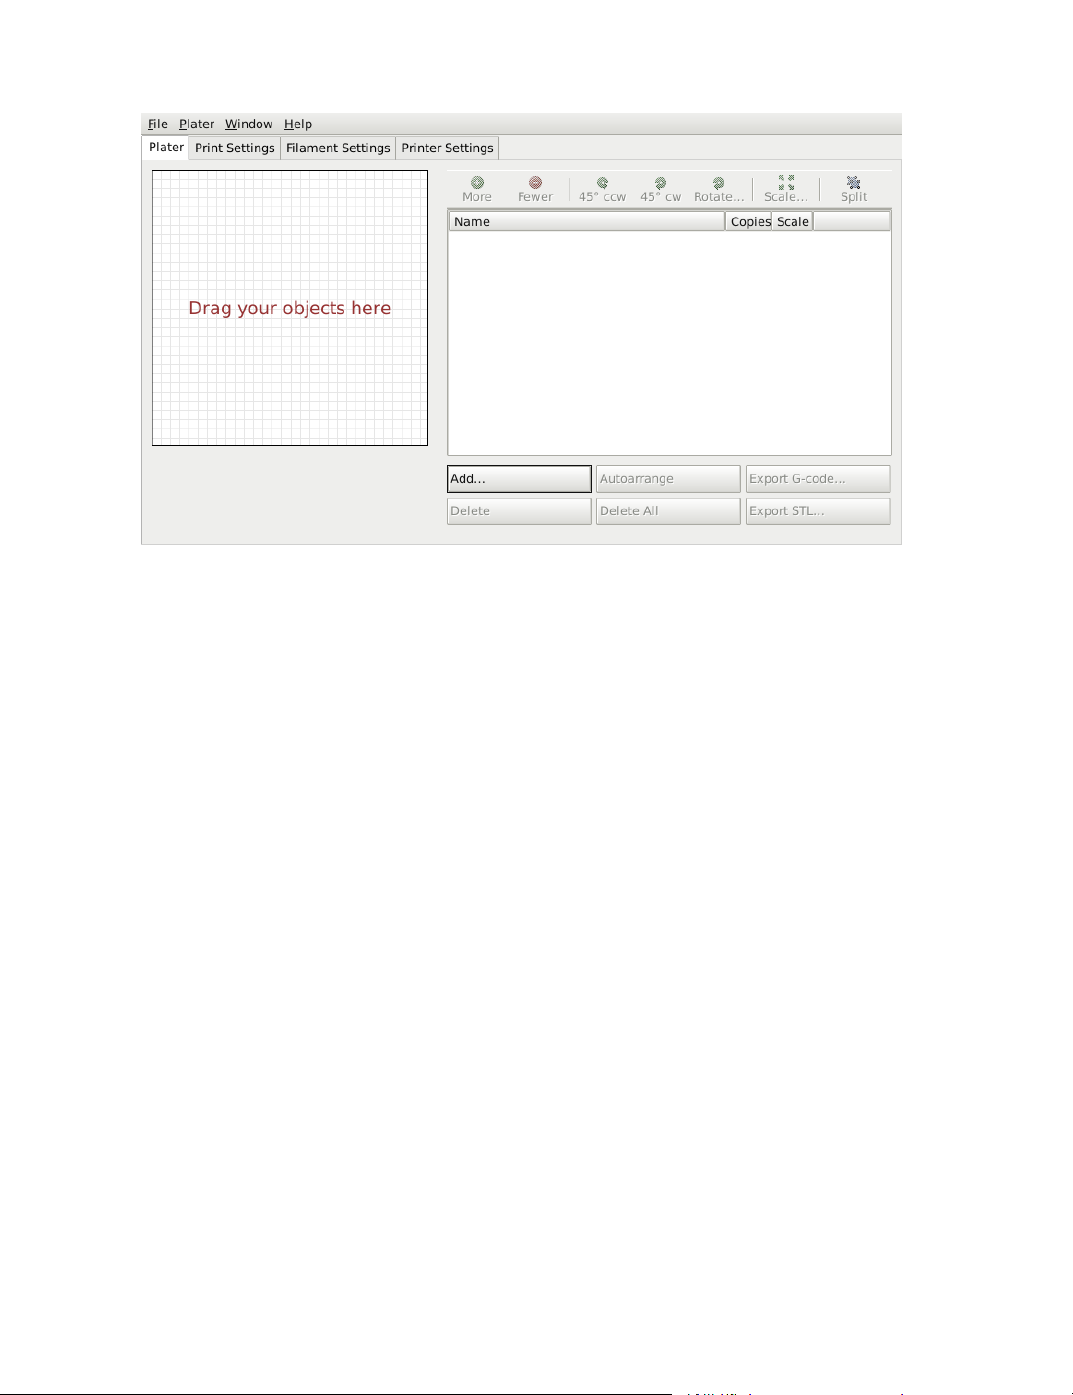
Slic3r
Figure 2.10: Plater
Once you have acquired a model, drag it onto the Plater window (or use
the Add button below the le list) to load it into Slic3r. In the gure below,
the traditional RepRap Minimug9is loaded, and is viewed from above. The
ring around the model is a skirt - a single perimeter, several millimeters
away from the model, which is extruded rst. This is useful in making sure
the plastic is owing smoothly from the nozzle when the model is starting
to be printed.
9
http://www.thingiverse.com/thing:18357
76
Page 77
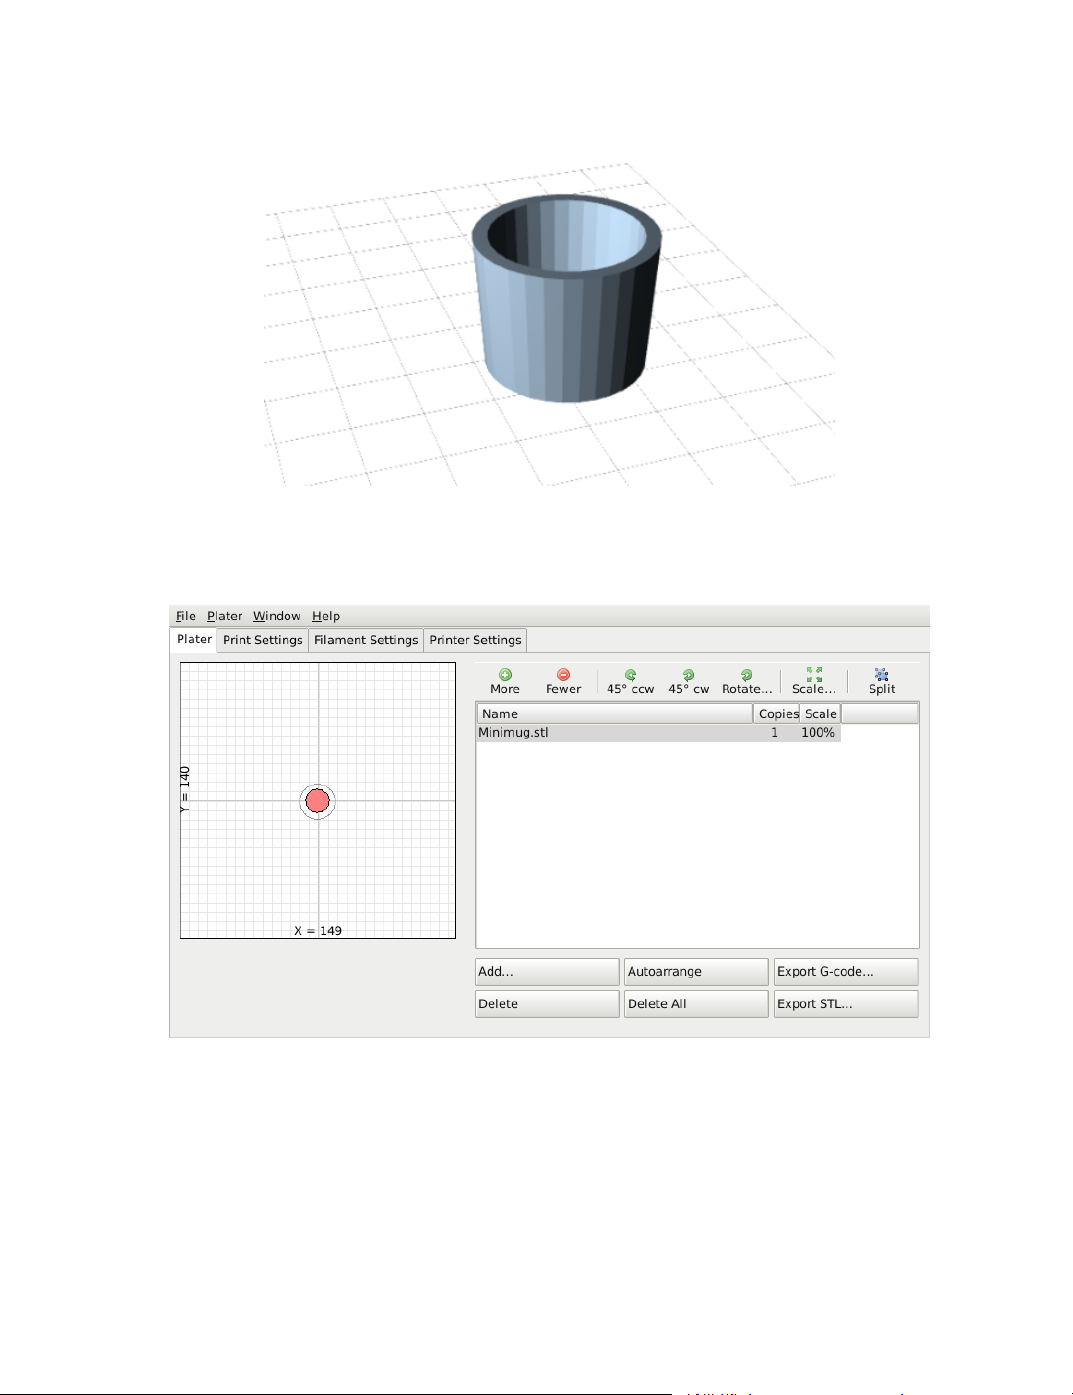
2.3. FIRST PRINT
Figure 2.11: Minimug model.
Figure 2.12: STL le loaded.
The model can be repositioned by dragging the representation of it on
the left of the screen around the bed. Note that the dimensions of the bed
should match your printer, as given during the initial conguration above.
77
Page 78
Slic3r
Turn o “Auto-center Parts” in Preferences to position parts where desired.
On the right-hand side is the list of currently loaded les. The buttons
along the top of the le list allow you to arrange the models.
• More/Less - Adjust how many copies should be printed.
• 45°/Rotate - Rotate the selected model around the Z axis, either in
45° increments clockwise or counter-clockwise, or by a given amount.
• Scale - Increase or decrease the size of the printed model.
• Split - Divides a model which consists of more than one part into it’s
constituent parts, allowing each one to be arranged individually.
• View/Cut - Provides a 3D view.
The buttons along the bottom of the le list allow you to add, remove,
auto-arrange, or export the models.
• Add - Opens a le dialog to add a model to the plater, as an
alternative to dropping a le directly.
• Delete/Delete All - Remove one or all models from the plater.
• Autoarrange - Attempt to arrange the models to give the optimal
layout.
• Export G-code - Starts slicing the model and produces a G-Code le.
• Export STL - Save the current set of models as a single STL le.
Cleaning STLs
If the 3D mesh described in the model contains holes, or edges are
misaligned (known as being non-manifold), then Slic3r may have problems
working on it. Slic3r will attempt to x any problems it can, but some
problems are out of its reach. If the application complains that a model
cannot be sliced correctly then there are several options available: see the
chapter about Repairing Models.
78
Page 79
2.4. SIMPLE MODE
Printing
At this stage Slic3r has been congured and a model has been acquired,
sliced and made ready for print. Now would be the time to re up the
printer and try it out.
A variety of host software is available to send the G-code to the
printer. Amongst the open-source solutions are: Printrun10, Repetier
11
and Repsnapper12.
The following subsections will cover the options available in expert
mode, and look at advanced printing techniques, including special cases
and troubleshooting.
2.4 Simple Mode
Simple Mode
Slic3r has two modes of operation, Simple and Expert. These may be
chosen from the Preferences window (found under the File menu).
Figure 2.13: Preferences.
Simple mode oers a reduced set of options, enough for the beginner to
get started with. Expert mode gives more control over how Slic3r produces
the G-code and will be looked at later.
Print Settings
The Print Settings tab provides the opportunity to change settings
related to the actual print. Whereas the other tabs are changed rarely,
the settings on this tab will be modied regularly, possibly for each model
printed.
10
https://github.com/kliment/Printrun
11
http://www.repetier.com/
12
https://github.com/timschmidt/repsnapper
79
Page 80
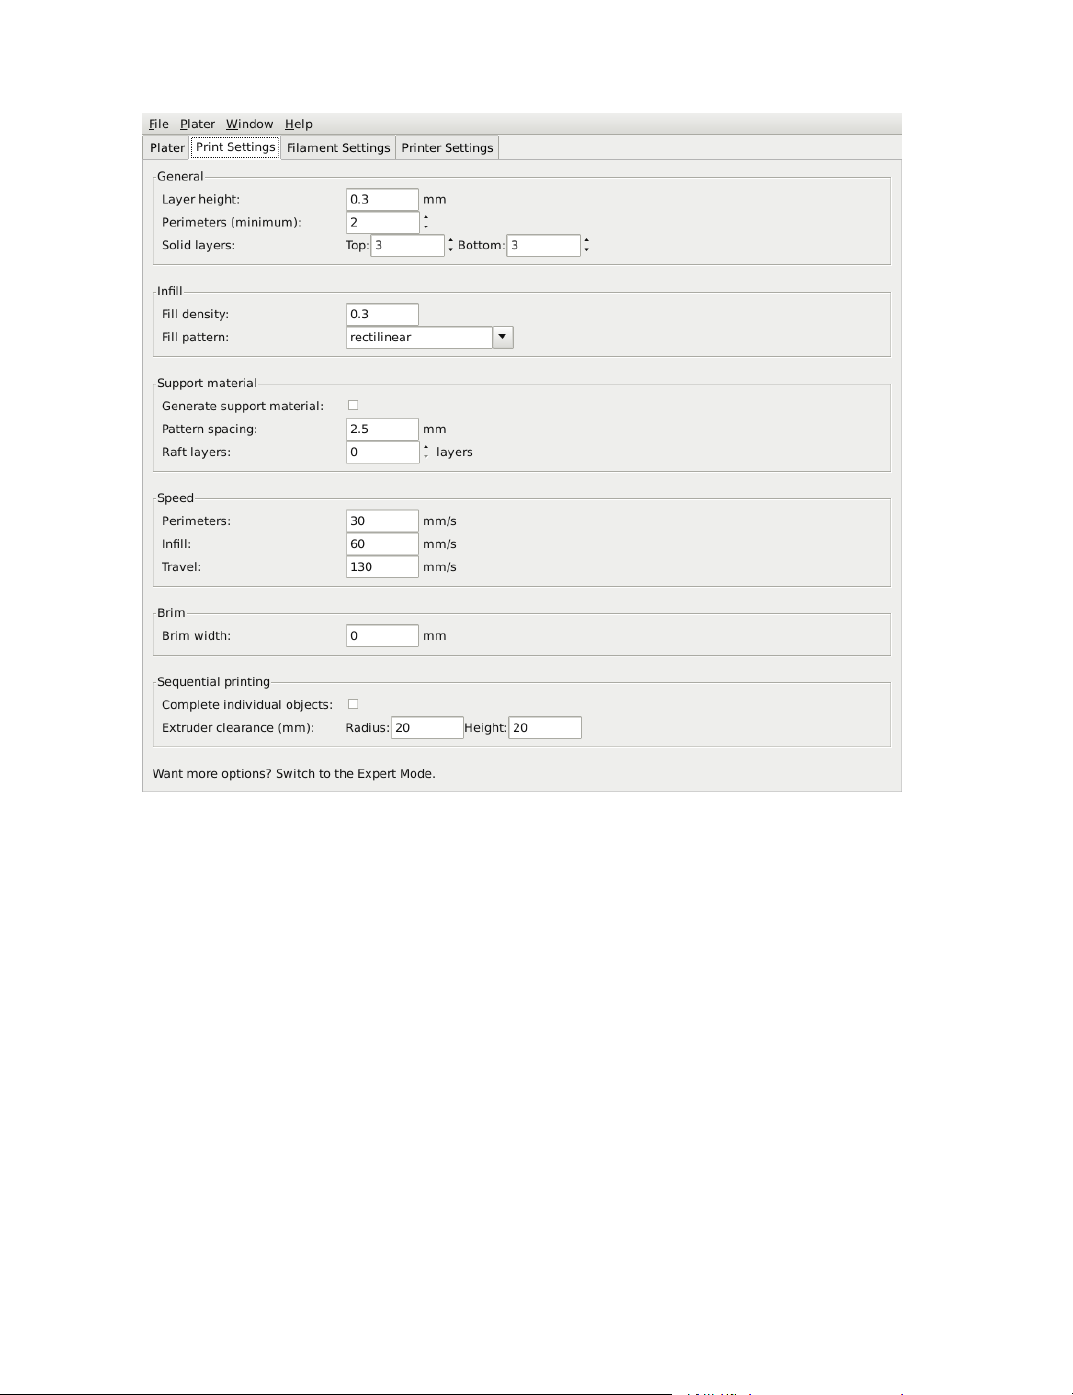
Slic3r
Figure 2.14: Simple Mode: Print Settings.
General. Layer height is the thickness of each layer, and it is the step
along the vertical axis taken before extruding a new layer atop the previous
one. There are several factors that inuence how high each layer should
be:
• Desired resolution - Lower layer height should result in prints with
less noticeable ribs or bands, as each layer is smaller. Aesthetics plays
a role here, but also the type of model, for example, a mechanical part
may not need such a high resolution nish, whereas a presentation
piece may do so.
80
Page 81
2.4. SIMPLE MODE
• Print speed - Shorter layers will result in smoother prints but each
print will take longer, simply because the extruder must trace the
pattern more times. A later goal will be to strike a balance between
layer height, the speed of the printer, and the quality of the resulting
print.
Perimeters denes the minimum number of vertical shells (i.e. walls) a
print will have. Unless the model requires single width walls it is generally
recommended to have a minimum of two perimeters as this gives some
insurance that if a subsection of the perimeter is not printed correctly then
the second perimeter will help cover it.
The upper and lowermost layers that sandwich the model are lled with
a Solid layers pattern. For the bottom layers the important factor to
consider is how the surface will look should there be a mistake whilst laying
down the rst layer, and for this reason it is recommended to have at least
two bottom layers.
A similar consideration is required for the top layers. Because the
intermediate layers are likely to be lled with a pattern set less than 100%
then the covering layers will have to bridge this pattern and this can require
more than one pass to cover completely.
Figure 2.15: An example of insucient top layers.
81
Page 82
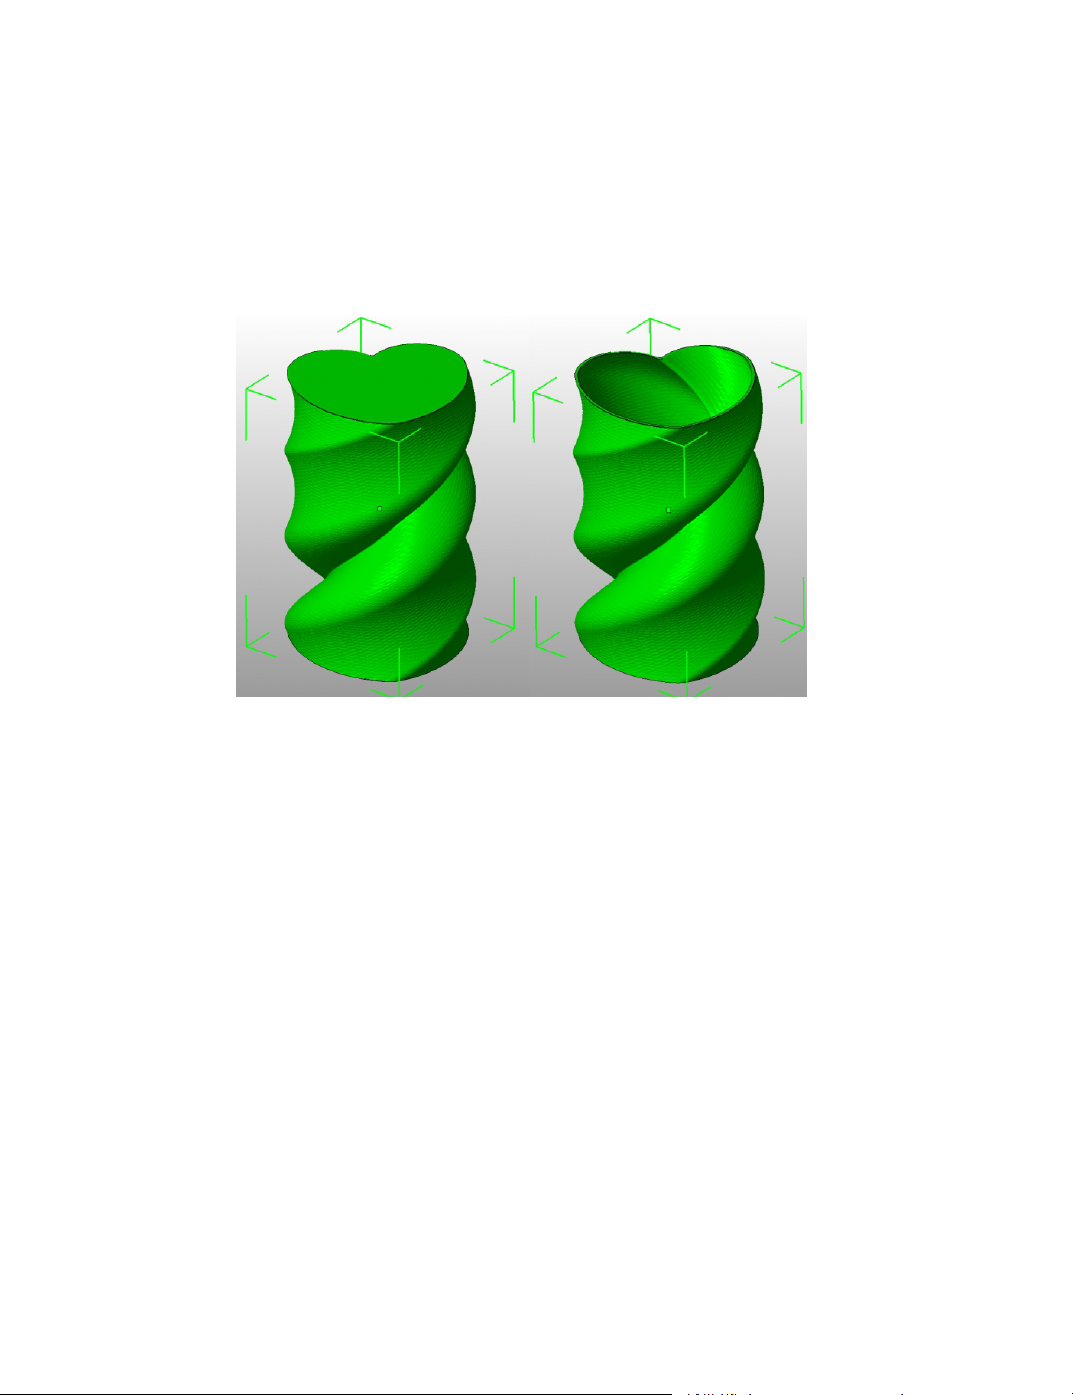
Slic3r
Another tip to consider: Setting the top solid layer to zero, and setting
the inll also to zero, will result in a hollow receptacle, ideal for turning
models into vases13for example. Here manipulating the settings within
Slic3r can be used to generate dierent kinds of prints, and not only be
used to control surface accuracy.
Figure 2.16: Creating a vase from a solid model.
Inll. Fill density is dened on a scale of between 0 and 1, where 1 is
100% and 0.4 would be 40%. For the majority of cases it makes no sense to
100% ll the model with plastic, this would be a waste of material and take
a long time. Instead, most models can be lled with less material which is
then sandwiched between layers lled at 100% (see Solid layers above).
A density value of 0.4 is enough to give almost all models good
mechanical strength. A value of 0.2 is usually the minimum required to
support at ceilings.
Slic3r oers several ll patterns which will be discussed in more depth
in subsection 2.5 - Inll Choices. Choosing a Fill pattern will depend
on the kind of model, the desired structural strength, print speed, and
personal taste. The more exotic ll methods are usually too slow and
unnecessarily complex for most use cases, and so most of the time the inll
13
http://slic3r.org/blog/tip-printing-vases
82
Page 83
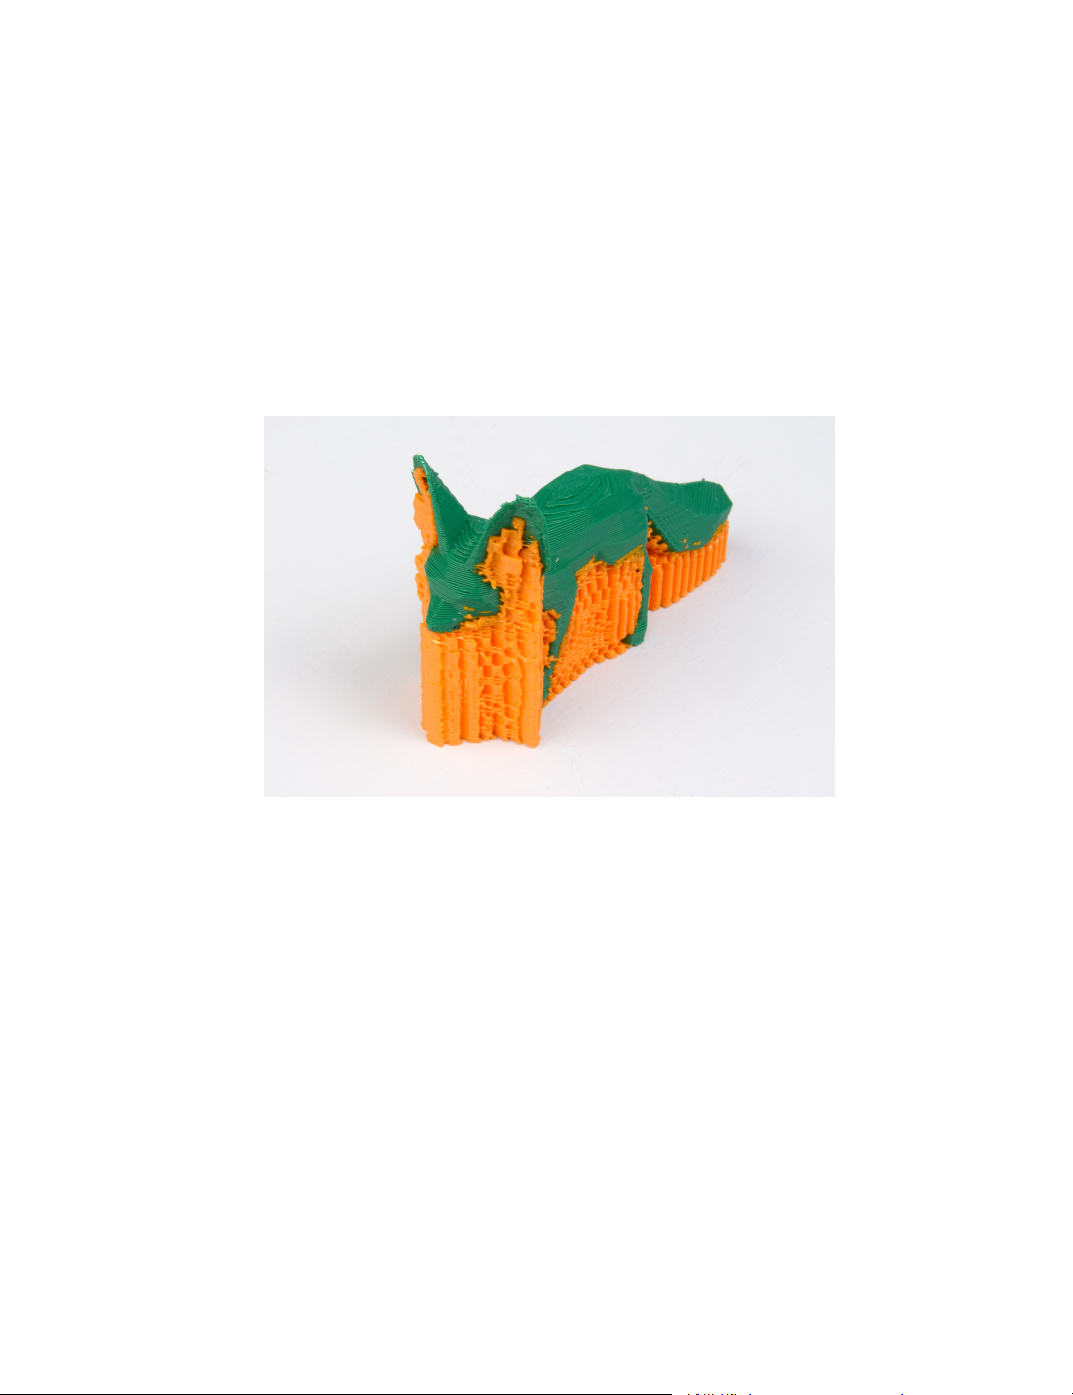
2.4. SIMPLE MODE
pattern is either rectilinear, line, or honeycomb. Honeycomb gives the
most strength but is slower than both rectilinear or line.
Support material. Printing a model from the bottom up, as with FDM,
means that any signicant overhangs will be printed in the air, and most
likely droop or not print correctly. Choosing support material (Generate
support material) will add additional structures around the model which
will build up to then support the overhanging part. The Pattern spacing
option determines how dense the support material is printed.
Figure 2.17: An example of an object printed with support material.
Tip: It is sometimes worth considering altering the orientation of the
model in order to possibly reduce overhangs.
Raft layers will add additional layers underneath the model and stems
from the early days of 3D printing. It can help with prints without a heated
bed, or where the bed is not very at, but it is usually not required and is
not recommended. The raft also requires post-processing to remove it.
Speed. In simple mode there are only three speed settings to consider:
• Perimeters - The outline of the model may benet from being
printed slightly slower so that the outside skin of the print has fewer
blemishes.
83
Page 84
Slic3r
• Infill - As the inll is hidden this can be extruded a little faster.
Take care though not to go too fast as higher speeds results in thinner
extrusions, and this may aect how the extrusions bond.
• Travel - The jump between the end of one extrusion and the next
should usually be performed as quickly as the printer will allow in
order to minimise any mess caused by material oozing from the nozzle.
Brim. Brim width is used to add more perimeters to the rst layer, as a
base ange, in order to provide more surface area for the print to stick to
the bed with in order to reduce warping (see §2.3). The brim is then cut
away once the print is nished and removed from the bed.
Figure 2.18: An example of brim.
Sequential Printing. This feature allows to compose a plate of objects but
have the printer complete each one individually before going back to Z
= 0 and starting with the next one. See the subsection about Sequential
Printing in the Advanced Topics chapter.
Filament Settings
The Filament Settings will normally be used infrequently, for example
on receipt of a new roll of lament.
84
Page 85
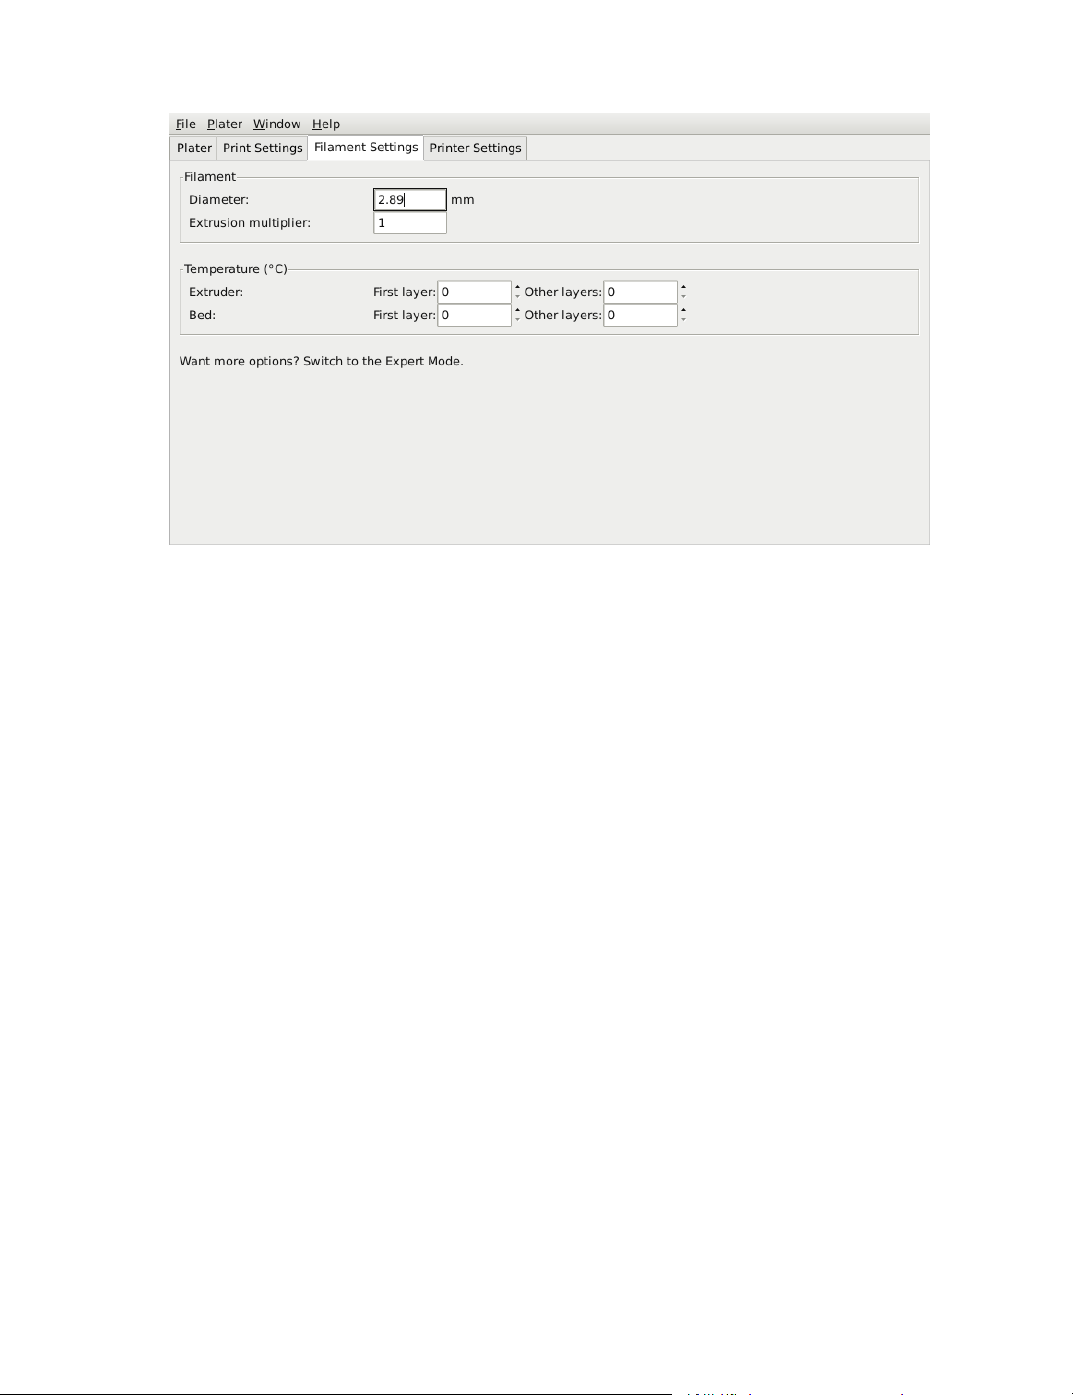
2.4. SIMPLE MODE
Figure 2.19: Simple Mode: Filament Settings.
Filament. The Diameter setting will already have been lled from the
value given during the wizard (see p.68), but can be updated here.
The Extrusion multiplier setting allows the ne tuning of the
extrusion ow rate, and is is given as a factor, e.g. 1 means 100%, 1.5
would mean 150%. Whilst the value should ideally be set in the rmware
it can be useful to test slight changes to the rate by altering this value. It
varies the amount of plastic proportionally and should be changed in very
small steps (e.g. +/- 0.05) as the eects are very visible.
Temperature. These values are also lled from the wizard, but here the
opportunity exists to set the temperature for the rst layer (see p.72).
Printer Settings
The Printer Settings will be updated the least, unless Slic3r is going to
be used for many printers, for example, in a 3D printer farm.
85
Page 86
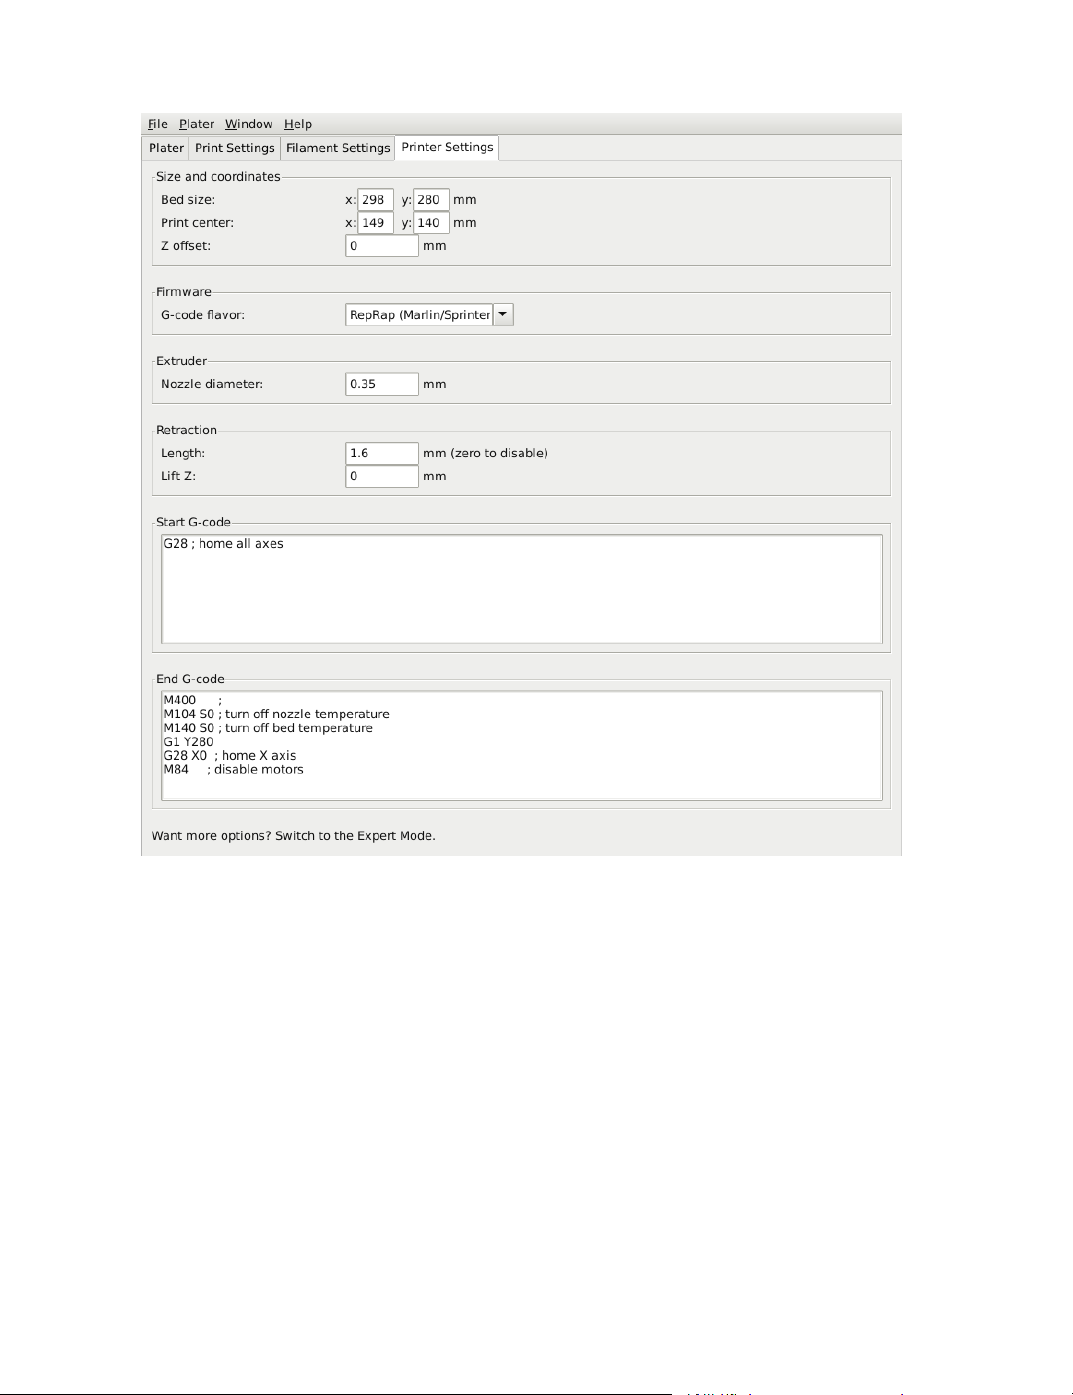
Slic3r
Figure 2.20: Simple Mode: Printer Settings.
Size and coordinates. The Bed size setting is taken from the wizard (see
p.66) and is only used for previewing the model in the plater.
The Print center is the point around which the print will be centered.
A Bed size of 200mmx200mm and a Print center of 100mmx100mm
would sit the print in the middle. Should it be desired to print away from
the center, because of a scratch in the glass perhaps, then this option should
be used.
Z offset can be used to compensate for an incorrectly calibrated Z
end-stop. If the nozzle stops slightly too far from the bed, then adding a
86
Page 87
2.4. SIMPLE MODE
negative value will oset all layers by that amount. The correct solution
however is to x the end-stop itself.
The optimal Z end stop position is where the nozzle tip barely touches
the surface of the bed when homed. A sheet of paper makes a good gauge
for this very small distance. It is not recommended to use this setting to
try and improve layer adhesion, by “squashing” the bottom layer into the
bed, instead look at the suggestions in subsection 2.3.
Firmware. As selected in the wizard (see p.65), G-code flavour denes
the dialect of G-code generated.
Extruder. Nozzle diameter was dened in the wizard (see p.67).
Retraction. Unless the material being extruded has a very high viscosity
it may ooze between extrusions due to gravity. This can be remedied by
actively retracting the lament between extrusions. Setting the Length
parameter to a positive value will cause the lament to be reversed by that
many millimeters before travel. The retraction will then be compensated
for by the same amount after the travel move, before starting the new
extrusion path.
A value of between 1 and 2mm is usually recommended. Bowden
extruders may need up to 4 or 5mm due to the hysteresis introduced by
the tube. Setting the Lift Z parameter to a positive value will raise the
entire extruder on the Z axis by that many millimeters during each travel.
This can be useful to ensure the nozzle will not catch on any already laid
lament, however it is usually not necessary and will slow the print speed.
A value of 0.1mm is usually sucient.
Start, End and Layer Chance G-codes. Custom G-code commands can be
run before a print starts and after a print nishes.
Placeholders can be inserted in the G-code commands14. For example
[next_extruder] would return the index of the next extruder.
The RepRap wiki is a good resource to learn about the variety of Gcodes available: http://reprap.org/wiki/G-code.
Note: Be sure to check that a given G-code is valid for your rmware.
14
https://github.com/alexrj/Slic3r/wiki/FAQ#what-placeholders-can-i-use-in-
custom-g-code
87
Page 88
Slic3r
The codes specied in Start G-code are inserted at the beginning of the
output le, directly after the temperature control commands for extruder
and bed. Note that if temperature control commands are specied (M104
and M190) then these will replace the temperature G-codes introduced by
the Filament settings.
Some common G-codes to use before the print starts are:
• G28 - Homes all the axes.
Some common G-codes to use after the print ends are:
• M104 S0 - Sets the extruder temperature to zero.
• M140 S0 - Sets the heated bed temperature to zero.
• G28 X0 - Home the X axis.
• M84 - Disables the motors.
2.5 Expert Mode
Speed
Once the printer is reliably producing good quality prints it may be
desirable to increase the speed. Doing this provides several benets, the
most obvious of which is that the results are produced quicker, but also
faster print times can be utilised in producing more layers, i.e. lower layer
height, thus improving perceived print quality. An additional benet is
that a faster travel movement, between extrusions, can reduce the eects
of oozing.
The best approach is to increment the various speed parameters in
small steps and observe the eect each change has on print quality. Travel
speed is a safe starting point, and it is not unrealistic to attain speeds
of up to 250mm/s (if your printer can handle it). Adjusting the speed of
perimeters, inll is available in simple mode, and the general rule is to have
the perimeter go a little slower than the inll in order to reduce possible
blemishes on the surface (inll can be faster because slight gaps will not
matter as much).
Expert mode oers more parameters to ne tune printer speeds. Differentiation between external, small and other perimeters, inll locations,
88
Page 89
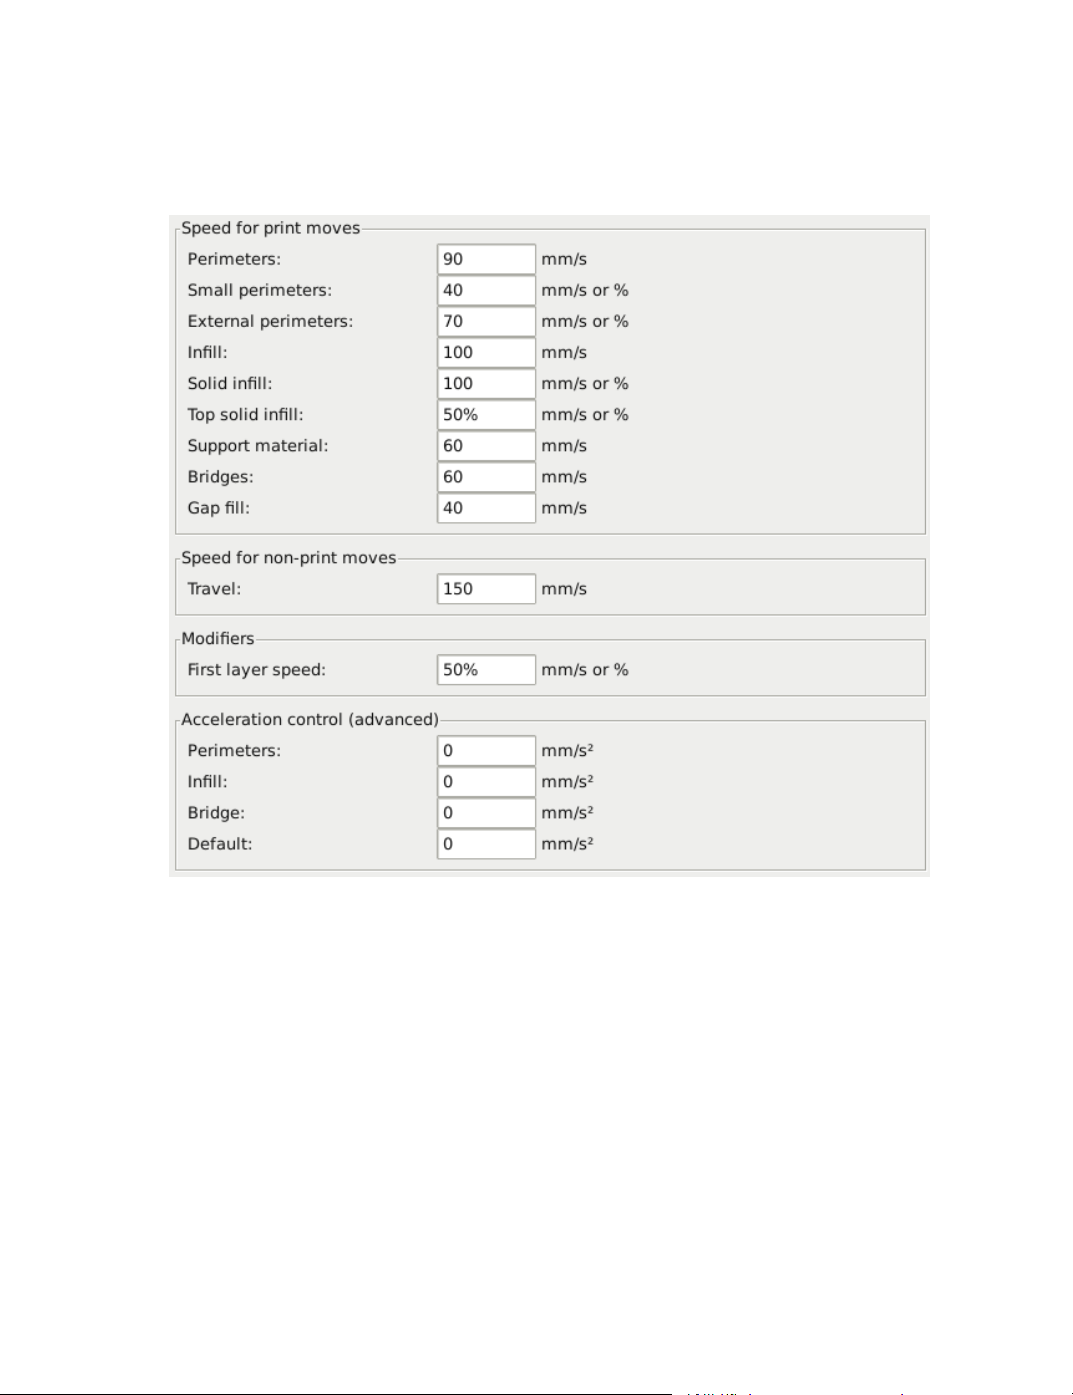
2.5. EXPERT MODE
and bridges and gaps are available, as well as the ability to slow down for
the rst layer.
Figure 2.21: Expert mode speed options.
Where indicated a value can be given in percentage. This is in relation
to the preceding value, e.g. 50% solid inll would be half of the value
dened for inll.
A few general guidelines for each option:
• Perimeters - In expert mode this parameter can be increased slightly
as the External perimeters option can be used to ensure blemish
free external faces.
89
Page 90
Slic3r
• Small perimeters - Meant for holes, islands and ne details, a slower
speed here is recommended.
• External perimeters - A slightly slower value may ensure cleaner
surfaces.
• Infill - As fast as you can without compromising the integrity of the
ll structure. Faster extrusions can break and result in weak spots.
• Solid infill - The bottom of the model, and any additional solid
layers is usually slightly slower than inll but faster than perimeters.
• Top solid infill - Allow time for the extrusion to cleanly cover
the previous top layers and result in a tidy top surface. The last few
layers should have bridged the inll structure nicely, preparing the
way for a neat nish.
• Support material - Generally support structures are quick and dirty,
and so long as the base is adequately supported they can be built as
quickly as they can.
• Bridges - Having the extrusion span distances depends on the
material and cooling. Going too slow will result in sagging, too fast
will result in broken strands. Experimentation is the key here, but
generally bridging runs slower than perimeters.
• Gap fill - Filling in small gaps results in the extruder quickly
oscillating and the resulting shaking and resonance could have a
detrimental aect on the printer. A smaller value here can guard
against this. A setting of zero disables gap lling completely.
• Travel - As fast as your printer will allow in order to minimise ooze.
• First layer speed - As mentioned in subsection 2.3, the rst layer is
important to lay down correctly, and a slower pace helps enormously.
Setting a value of 50%, or even less, can really help.
Acceleration control is an advanced setting allowing acceleration
settings for perimeters, inll, bridge, as well as a default setting, to be
made. Deciding which values to set depends on the capabilities of the
machine. Any settings within the rmware may be a good starting point.
90
Page 91
2.5. EXPERT MODE
Take into account any restrictions enforced by the rmware as many
have settings for the maximum safe speed of each axis.
91
Page 92
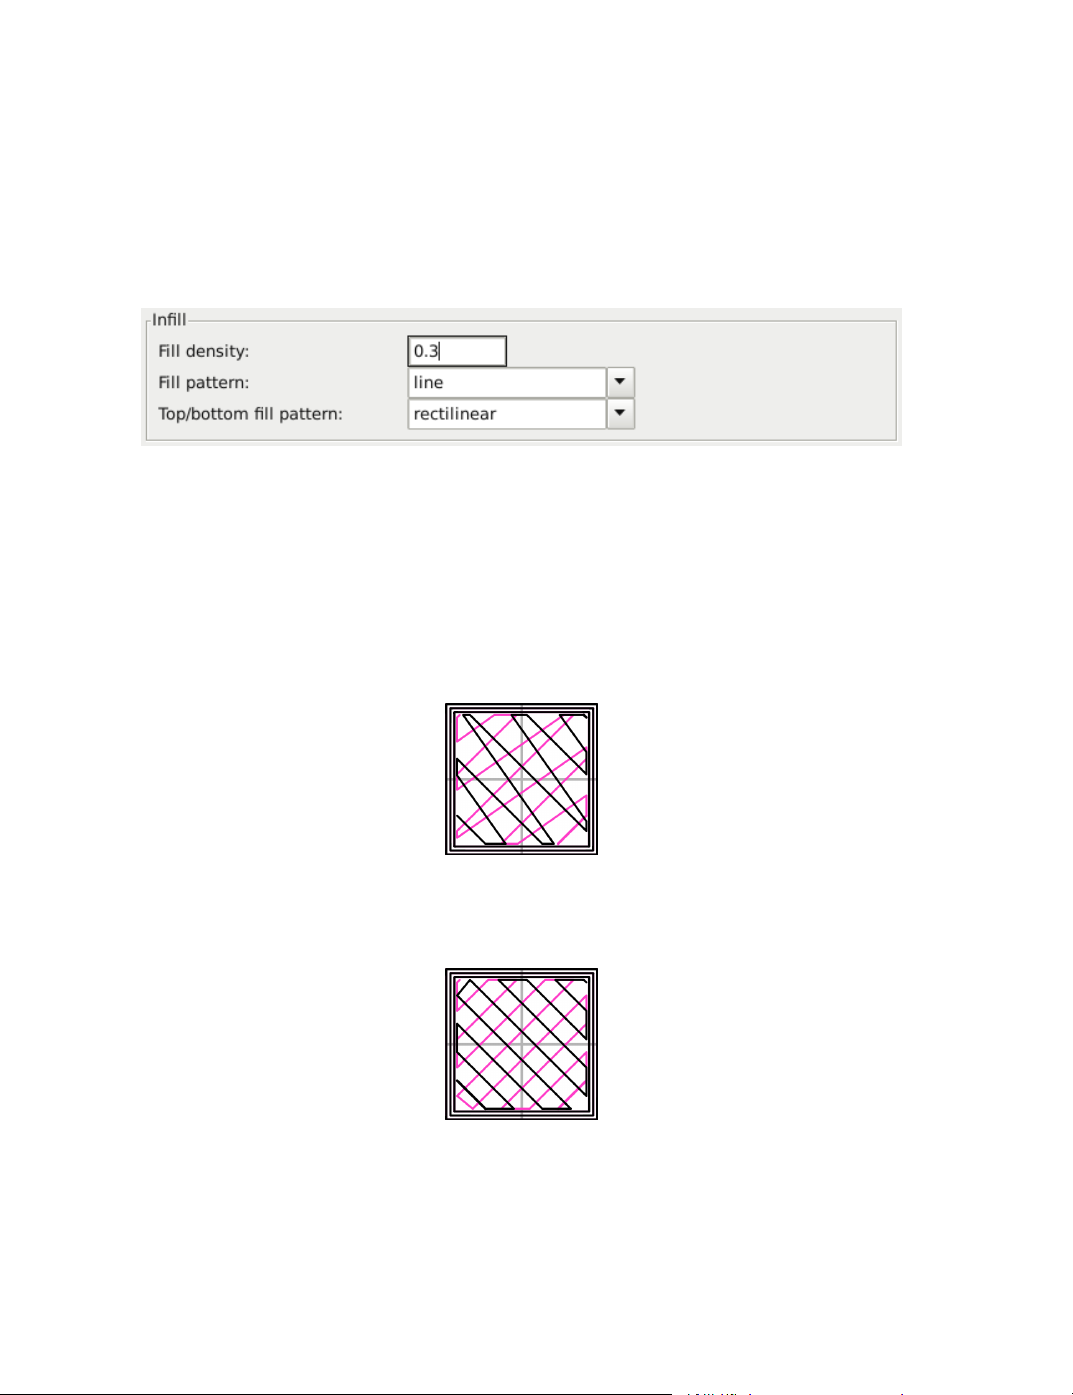
Slic3r
Inll Patterns and Density
There are several considerations when choosing an inll pattern: object
strength, time and material, personal preference. It can be inferred that a
more complex pattern will require more moves, and hence take more time
and material.
Figure 2.22: Inll pattern settings.
Slic3r oers several inll patterns, four regular, and three more exotic
avours. The numbers given in brackets below each gure are a rough
estimate of material used and time taken for a simple 20mm cube model15.
Note that this is only indicative, as model complexity and other factors
will aect time and material.
Figure 2.23: Inll pattern: Line (344.51mm / 5m:20s)
Figure 2.24: Inll pattern: Rectilinear (350.57mm / 5m:23s)
15
Taken from http://gcode.ws
92
Page 93
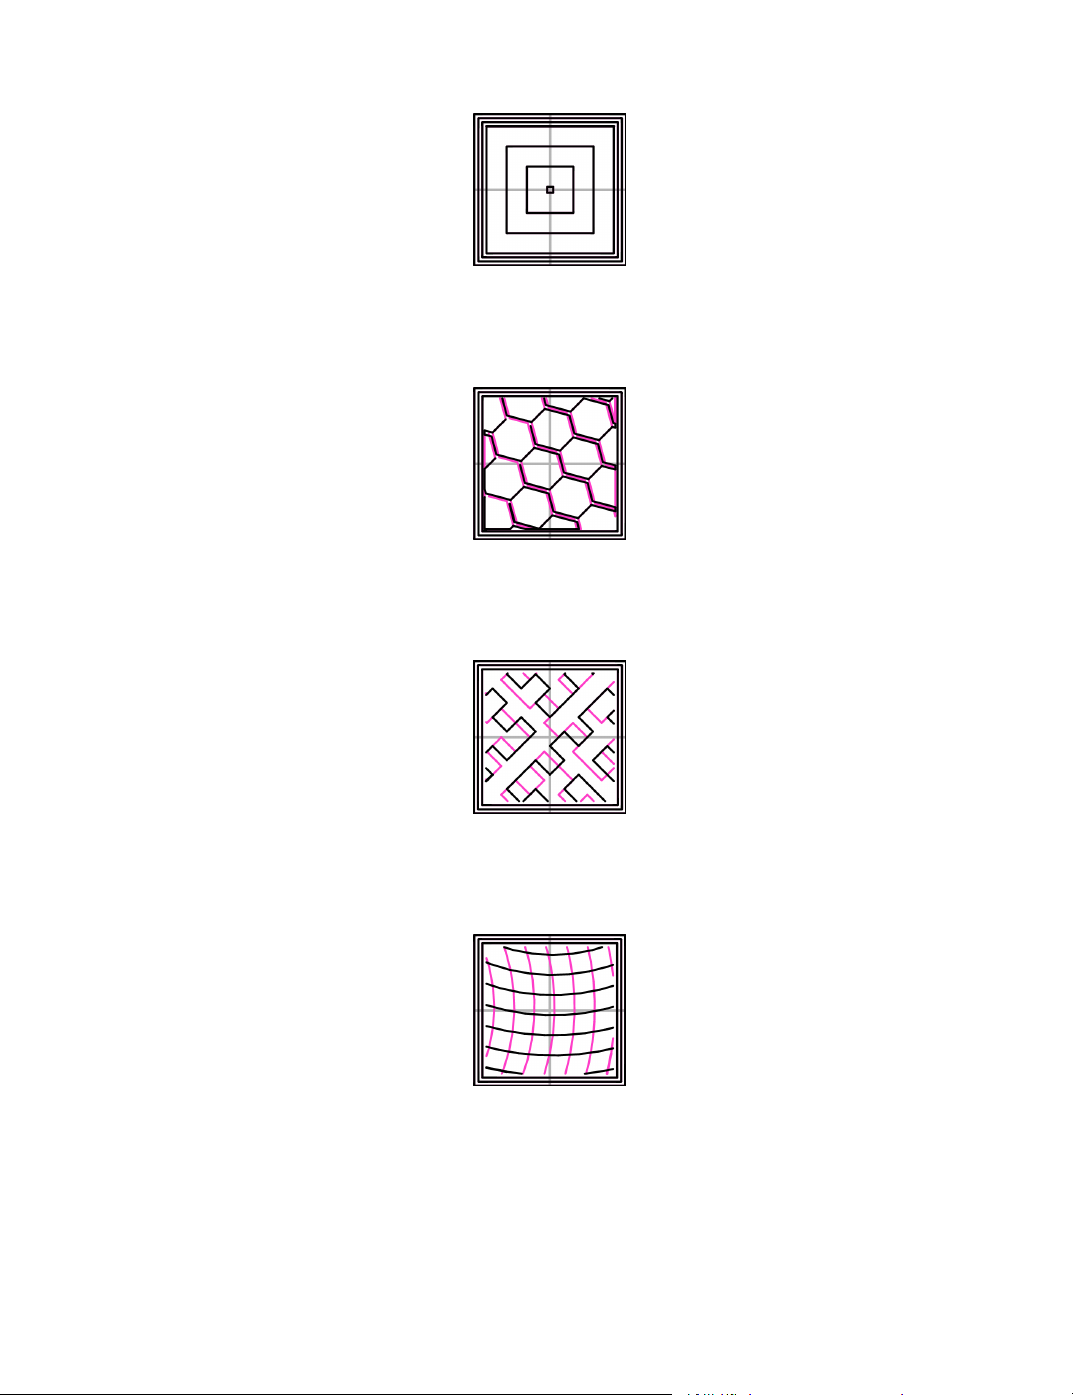
2.5. EXPERT MODE
Figure 2.25: Inll pattern: Concentric (351.80mm / 5m:30s)
Figure 2.26: Inll pattern: Honeycomb (362.73mm / 5m:39s)
Figure 2.27: Inll pattern: Hilbert Curve (332.82mm / 5m:28s)
Figure 2.28: Inll pattern: Archimedean Chords (333.66mm / 5m:27s)
93
Page 94
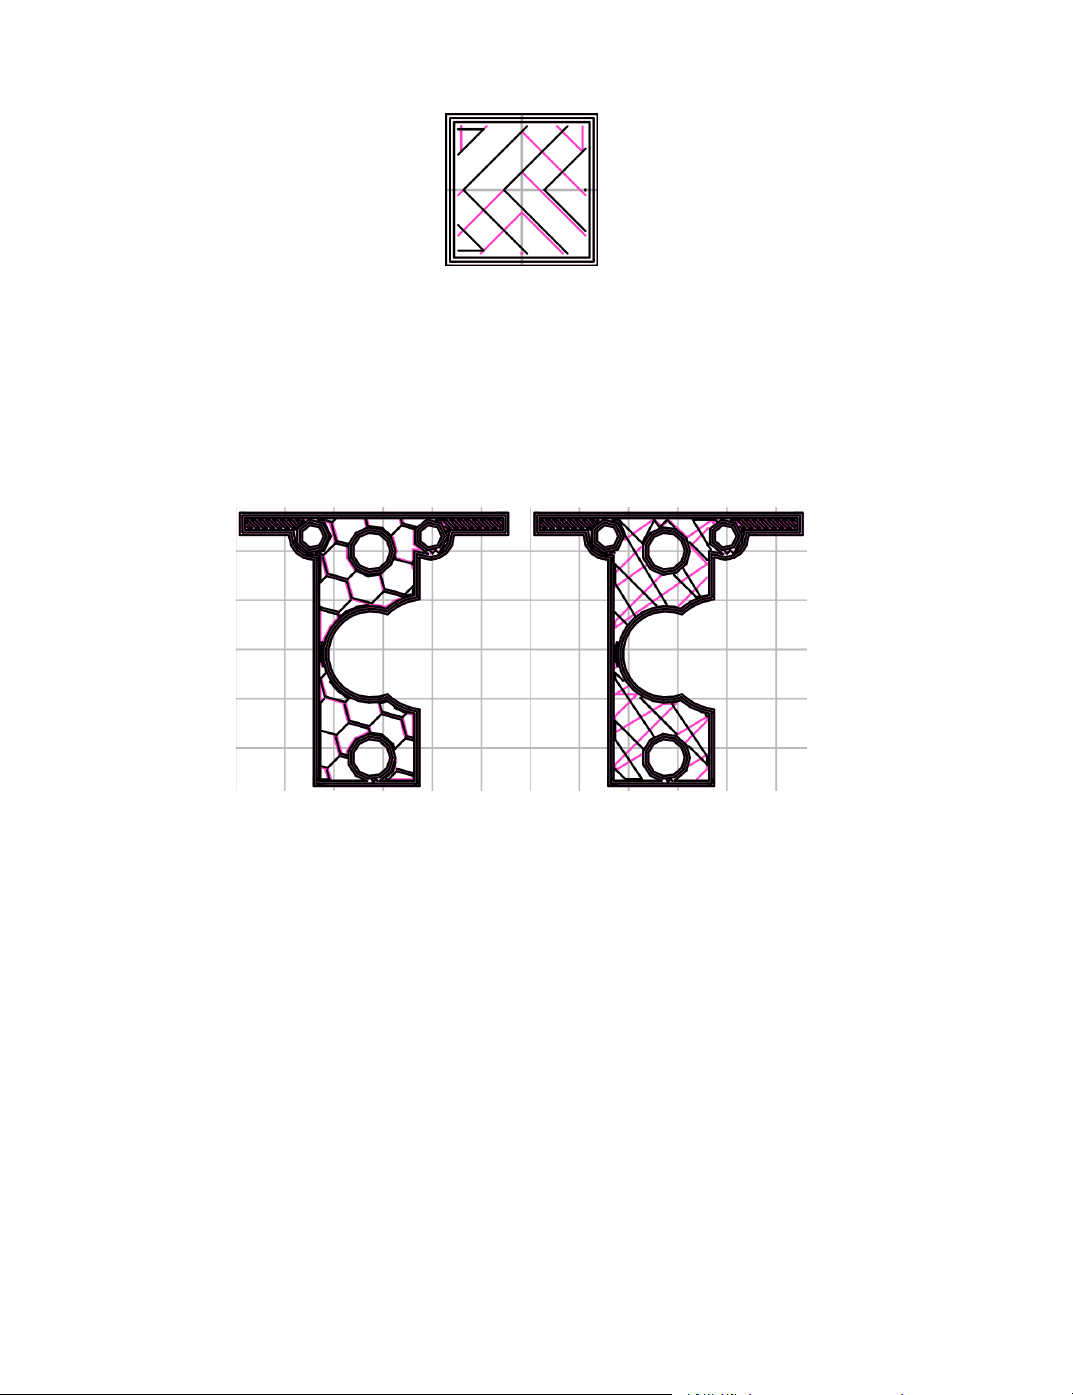
Slic3r
Figure 2.29: Inll pattern: Octagram Spiral (318.63mm / 5m:15s)
Certain model types are more suited for a particular pattern, for example organic versus mechanical types. Figure 2.30 shows how a honeycomb
ll may suit this mechanical part better because each hexagon bonds with
the same underlying pattern each layer, forming a strong vertical structure.
Figure 2.30: Inll pattern comparison in a complex object. Left to Right:
honeycomb, line
Most models require only a low density inll, as providing more than,
say, 50% will produce a very tightly packed model which uses more material
than required. For this reason a common range of patterns is between 10%
and 30%, however the requirements of the model will determine which
density is best. Figure 2.31 shows how the patterns change as the density
increases.
94
Page 95
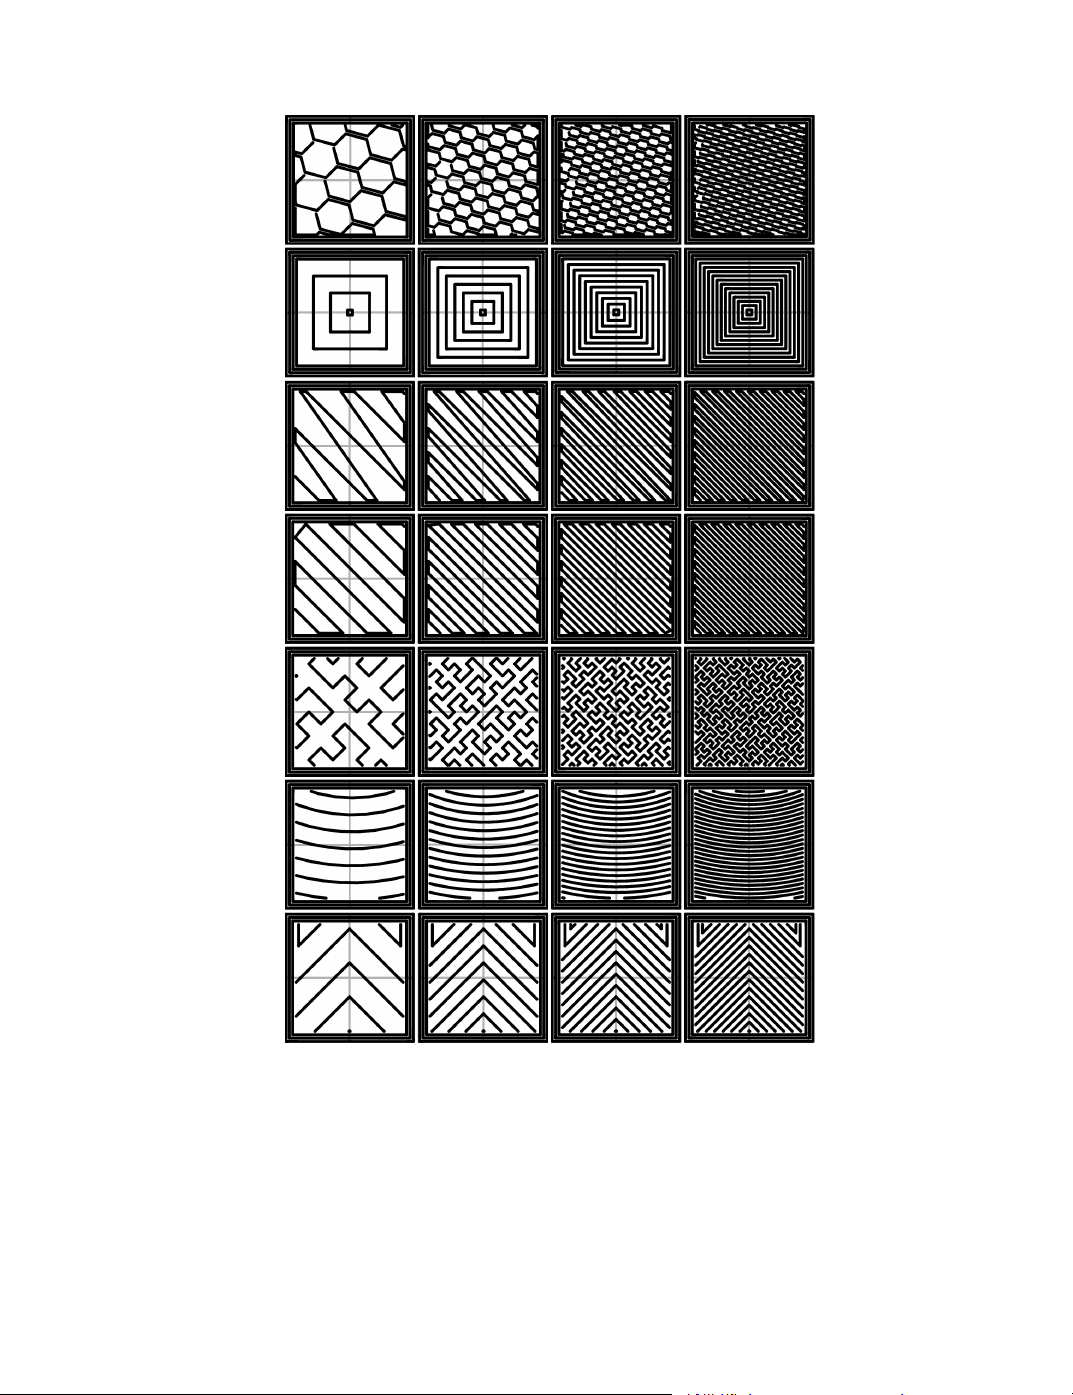
2.5. EXPERT MODE
Figure 2.31: Inll patterns at varying densities. Left to Right:
20%,40%,60%,80%. Top to Bottom: Honeycomb, Concentric, Line, Rectilinear, Hilbert Curve, Archimedean Chords, Octagram Spiral
95
Page 96
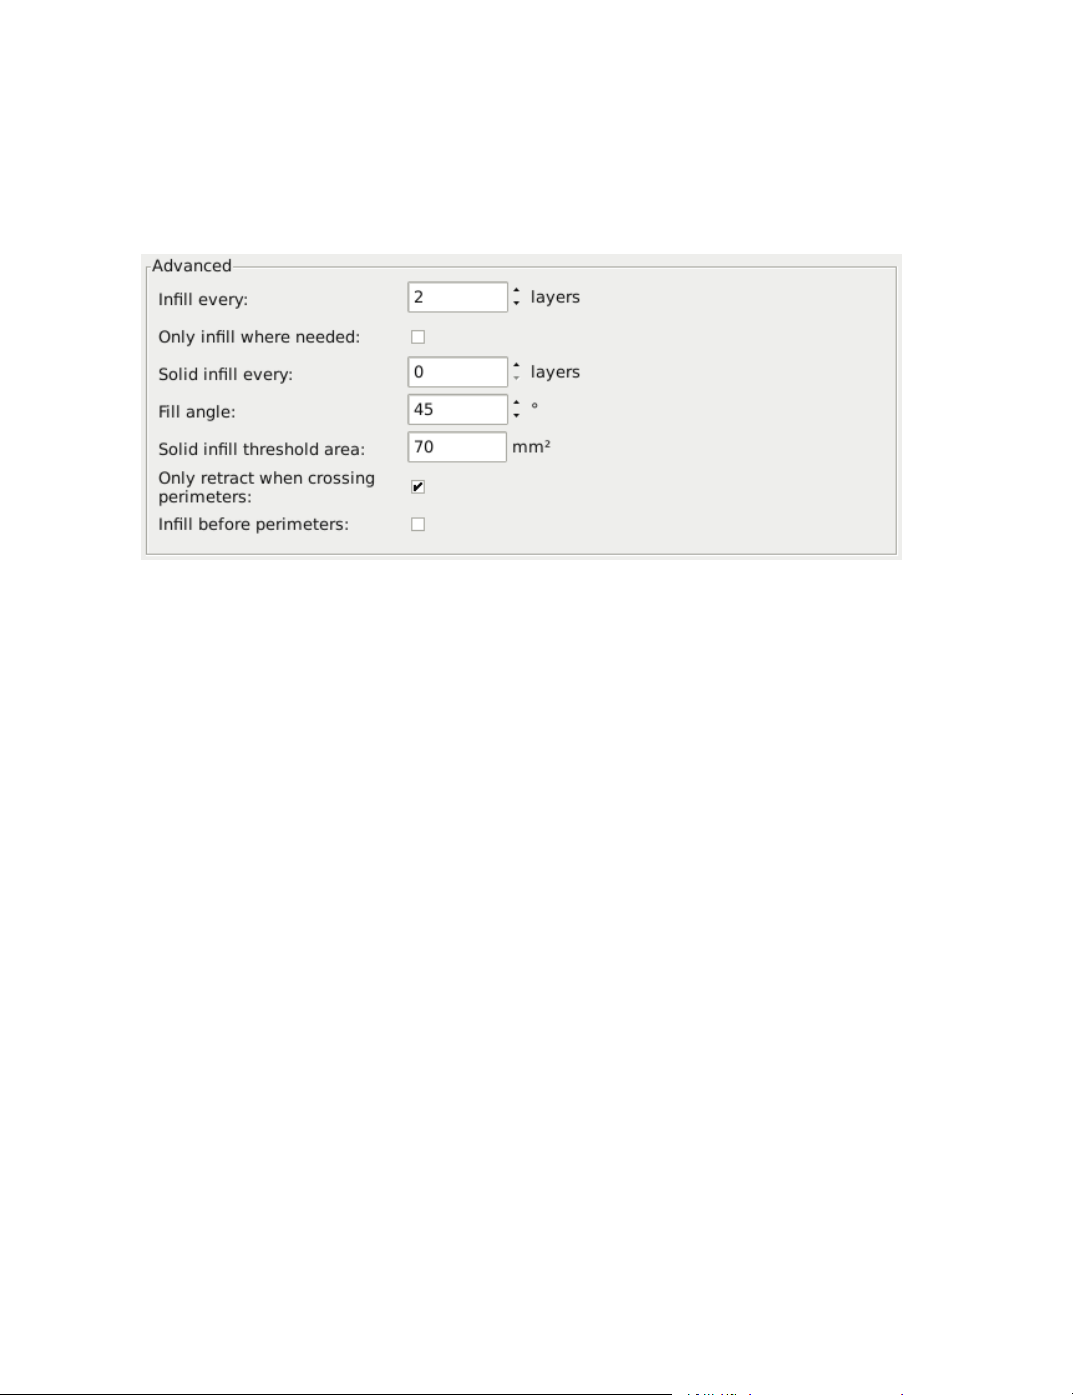
Slic3r
Inll Optimization
Slic3r contains several advanced inll settings which can help produce
better extrusions.
Figure 2.32: Inll advanced settings.
• Infill every n layers - Will produce sparse vertical inll by
skipping a set number of layers. This can be used to speed up print
times where the missing inll is acceptable.
• Only infill where needed - Slic3r will analyse the model and
choose where inll is required in order to support internal ceilings
and overhangs. Useful for reducing time and materials.
• Solid infill every n layers - Forces a solid ll pattern on the
specied layers. Zero will disable this option.
• Fill angle - By default the inll pattern runs at 45° to the model to
provide the best adhesion to wall structures. Inll extrusions that run
adjacent to perimeters are liable to de-laminate under stress. Some
models may benet from rotating the ll angle to ensure the optimal
direction of the extrusion.
• Solid infill threshold area - Small areas within the model are
usually best o being lled completely to provide structural integrity.
This will however take more time and material, and can result in
96
Page 97
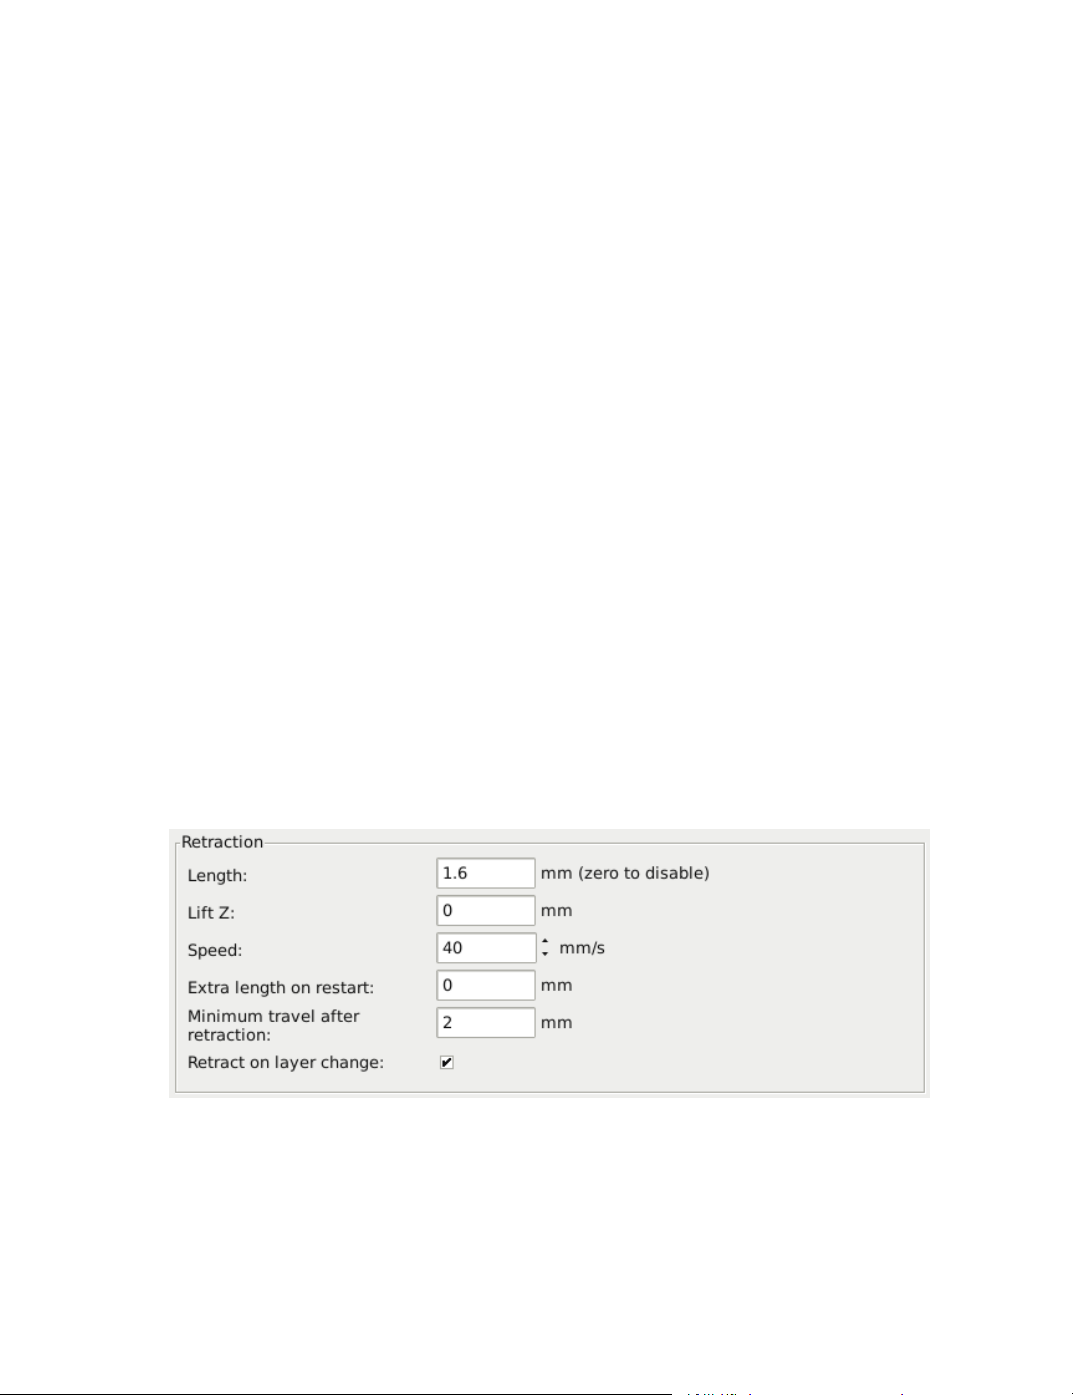
2.5. EXPERT MODE
parts being unnecessarily solid. Adjust this option to balance these
needs.
• Only retract when crossing perimeters - Retracting, to prevent
ooze, is unnecessary if the extruder remains within the boundaries
of the model. Care should be taken if the print material oozes
excessively, as not retracting may result in enough material loss to
aect the quality of the subsequent extrusion. However, most modern
printers and materials rarely suer from such extreme ooze problems.
• Infill before perimeters - Reverses the order in which the layer
is printed. Usually the perimeter is laid down initially, followed by
the inll, and this is usually the preferable as the perimeter acts as a
wall containing the inll.
Fighting Ooze
Unless the material being extruded has a very high viscosity it will ooze
from the nozzle in between extrusions. There are several settings in Slic3r
to which can help to remedy this.
The retraction settings, found in the Printer tab, tell the printer to pull
back the lament between extrusion moves. This can alleviate the pressure
in the nozzle, thus reducing ooze. After the subsequent travel move the
retraction is reversed to prepare the extruder for the next extrusion.
Figure 2.33: Retraction settings.
97
Page 98
Slic3r
• Length - The number of millimeters to retract. Note that the
measurement is taken from the raw lament entering the extruder.
A value of between 1 and 2mm is usually recommended. Bowden
extruders may need up to 4 or 5mm due to the hysteresis introduced
by the tube.
• Lift Z - Raises the entire extruder on the Z axis by that many
millimeters during each travel. This can be useful to ensure the nozzle
will not catch on any already laid lament, however it is usually not
necessary and will slow the print speed. A value of 0.1mm is usually
sucient.
• Speed - The speed at which the extruder motor will pull back the
lament. The value should be set to as quick as the extruder can
handle without skipping steps, and it is worth experimenting with
this value to nd the quickest retraction possible.
• Extra length on restart - Adds an extra length of lament after
the retraction is compensated after the travel move. This setting
is rarely used, however should the print show signs of not having
enough material after travel moves then it may be useful to add a
small amount of additional material.
• Minimum travel after retraction - Triggering a retraction after
very short moves is usually unnecessary as the amount of ooze is
usually insignicant and it slows down the print times. Set the
number of millimeters minimum distance the nozzle must move before
considering a retraction. If the printer handles ooze well this can be
increased to 5 or 6mm.
• Retract on layer change - Movement along the Z axis must also
be considered when dealing with oozing, otherwise blobs may occur.
It is recommended to leave this setting on.
• Wipe before retract - Moves the nozzle whilst retracting so as to
reduce the chances of a blob forming.
Additionally there are several settings in the Print tab which can help
control oozing.
98
Page 99
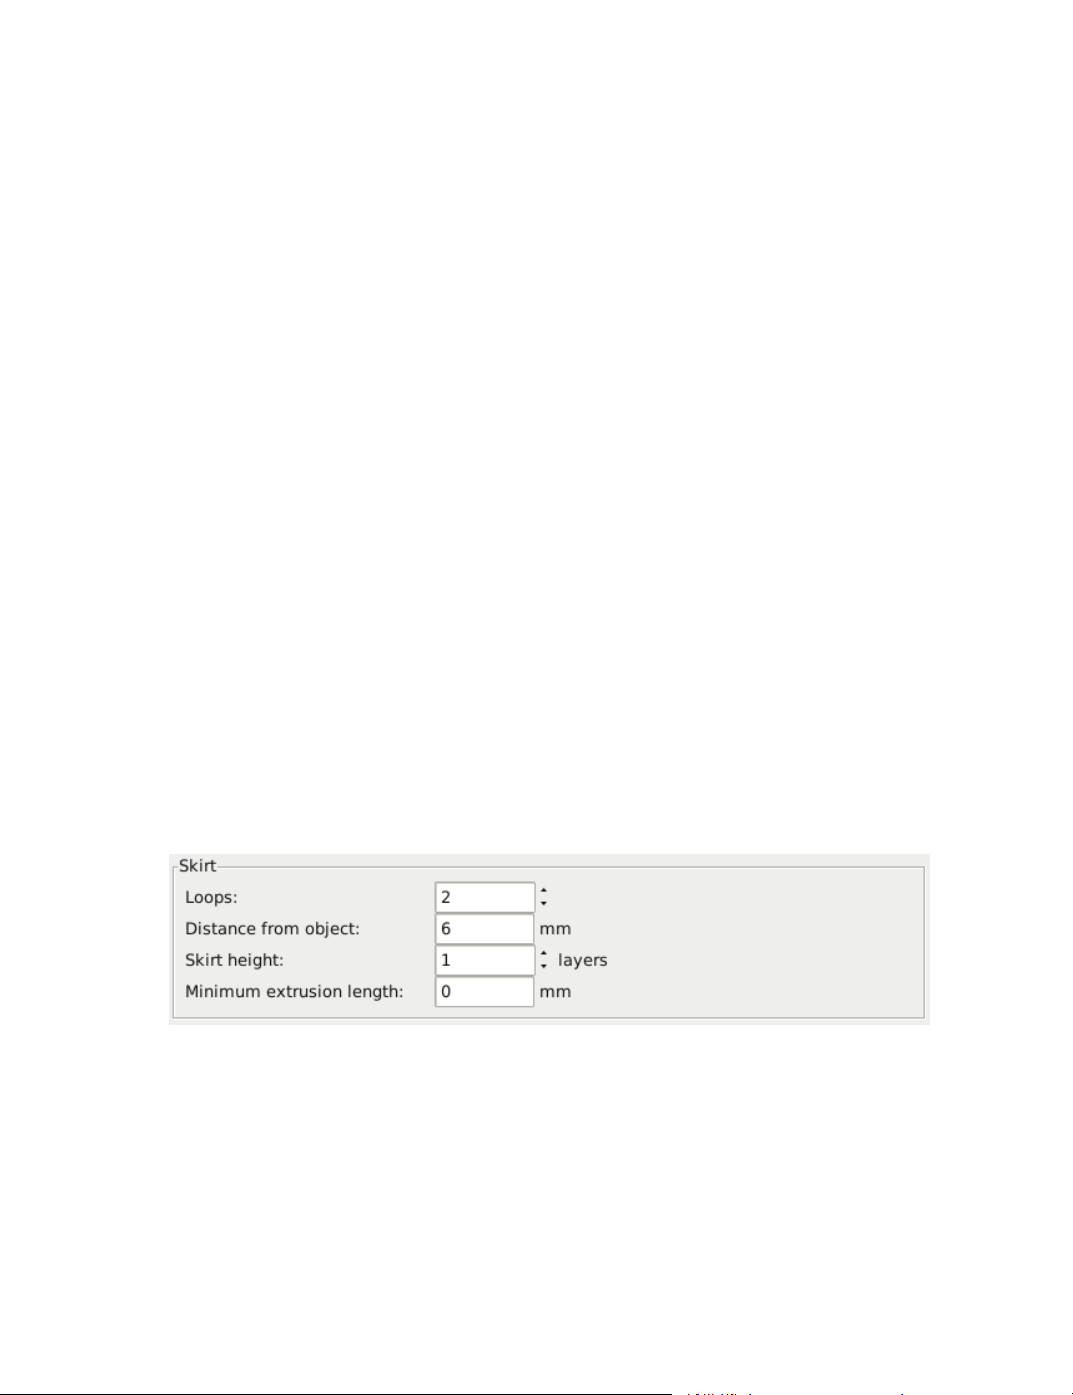
2.5. EXPERT MODE
• Only retract when crossing perimeters (Inll) - Tells Slic3r to
only retract if the nozzle will cross the threshold of the current island
being extruded. Slight ooze within the walls of a part are not seen
and can usually be accepted.
• Avoid crossing perimeters (Layers and perimeters - Advanced)
- Will force the nozzle to follow perimeters as much as possible
to minimise the number of times it must cross them when moving
around, and between, islands. This has a negative impact on both
G-code generation and print times.
• Randomize starting points (Layers and perimeters - Vertical shells)
- As the extruder moves up to the start of the next layer any ooze can
result in blobs. If the same start point is used for every layer then a
seam can form the length of the object. This setting will move the
start point to a dierent location for each layer.
See also subsection: Sequential Printing, on page 120 for another
technique which can minimise strings forming between objects.
Skirt
The Skirt setting adds an extrusion a short distance away from the
perimiter of the object. This can ensure that the material is owing
smoothly from the extruder before it starts on the model proper.
Figure 2.34: Skirt settings.
• Loops - How many circuits should be completed before starting on
the model. One loop is usually sucient.
99
Page 100
Slic3r
• Distance from object - The millimeters between the object and
the skirt. The default of 6mm is usually sucient.
• Skirt height - The number of layers to lay down a skirt for. For
ensuring the material is owing smoothly, one layer is sucient,
however the skirt function can also be used to build walls around
the object in case it should be protected from drafts.
• Minimum extrusion length - Dictates a minimum number of millimeters that the skirt should be, should the loop around the object
not be enough.
Cooling
Temperature plays a key part in determining print quality. Too hot and
the material deforms, too cool and layer adhesion may be problematic.
Applying cooling will allow the freshly deposited material to solidify enough
to provide a good base for the next layer, helping with overhangs, small
details and bridges.
There are two main techniques for cooling: adding a fan and slowing
down the print speed. Slic3r may choose to use both techniques, using a
fan rst, and then slowing down the print if the layer time is too fast.
100
 Loading...