

Page 1
Operating Manual
for
ForceCut™ 60i and 80i
IGBT Pilot Arc
Plasma Cutters
Page 2
Page 3
ForceCut™ 60i and 80i Plasma Cutters
Table of Content
Pg. i
Thank you From LONGEVITY®
Pg. ii
Warranty/Shipping Damage/Order Information
Pg. 1-2
Introduction
Pg. 3
Warning and Safety Tips
Pg. 4-5
Specifications and Ratings
Pg. 6
What’s Included?
Pg. 7-8
Basic Diagram, Wiring, and Setup Instructions
Pg. 9-12
Main Unit Knob/Button/Function
Pg. 13
Assembly of Plasma Cutter Torches
Pg. 14-15
Basic Plasma Cutter Operation
Pg. 16
Summary Chart of All LONGEVITY Plasma Cutters
Pg. 17-18
Features Chart of All LONGEVITY Plasma Cutters
Pg. 19
Typical Applications of All LONGEVITY Plasma Cutters
Pg. 20
Cutting Methods
Pg. 21
Tips and Advice for LONGEVITY Plasma Cutting by
www.plasma-cutters.com and www.freeweldingforum.com
Pg. 22-27
Routine Maintenance
Pg. 28
Troubleshooting
Pg. 29
Conclusion
Pg. 30
Table of Contents
www.longevity-inc.com i
Page 4
PLASMA CUTTERS www.LWELD.com
THANK YOU!
We, at LONGEVITY®, want to thank you for purchasing our product. You are
almost ready to experience LONGEVITY® Welding first hand. LONGEVITY®
definitely appreciates your business and understand that this equipment may be
overwhelming to setup and operate so we have prepared a manual that will assist you
in understand your new plasma cutter/welder. If you have any questions during or
after reading this manual, please feel to contact us! Please take a moment to register
your product on our website at www.longevity-inc.com or www.lweld.com
Once again, thank you for choosing LONGEVITY® as your main welding supplier!
LONGEVITY® Global, Inc
23591 Foley St
Hayward, CA 94545
Toll-Free Customer Support: 1-877-LONG-INC / 1-877-566-4462
Website: www.longevity-inc.com
Sales: [email protected]
Customer Service: [email protected]
Dealers: [email protected]
Complaints: [email protected]
Please join our welding forums to share welding tips and tricks, to receive useful
information from customers who also use our products, and to be a part of the
LONGEVITY® welding community at www.freeweldingforum.com
ii www.longevity-inc.com
Page 5
Plasma Cutters www.LWELD.com
W
arranty
LONGEVITY Plasma Cutters, Welders, and Multi-Purpose Welders are covered for
specific Parts and Labor warranty at our facility. For detailed information regarding
your specific LONGEVITY welder or cutter, please view our Terms and Policies
page on our website at the following website link: http://www.longevity-
inc.com/terms/
.
Shipping Damage
Your machine is insured against damage during shipping. Keep all packing materials
and containers in case machine must be returned. We will initiate a claim with the
shipping company to cover damage or loss. If there is shipping damage upon
opening your package, our customer service team will work with you to get the
matter resolved.
www.longevity-inc.com 1
Page 6
PLASMA CUTTERS www.LWELD.com
In Warranty Service
Customers, who own machines that are in warranty and require service, should
contact our Warranty Department by email at [email protected] to obtain a
return authorization code. When doing so, please provide the following information:
Order No.: _________________________________
Serial No: _________________________________
Date of Purchase: ____________________________
Warranty Period: ____________________________
Unit Tested Prior to Shipment By: _____________________________
Out-of-Warranty Service
Customers, who own machines that are out of warranty and require service, should
contact us for an estimate. LONGEVITY offers an exchange program on out of
warranty units. We also help non LONGEVITY customers with repairs, replacement,
and service.
If your unit is not manufactured by LONGEVITY® and you cannot receive service
from your manufacturer or seller, LONGEVITY® is here to help. Our warranty
policy is also available for all plasma cutters and welders. For more information,
please email us at [email protected]
2 www.longevity-inc.com
Page 7
Plasma Cutters www.LWELD.com
Introduction
The LONGEVITY® ForceCut™ series plasma cutters offer a revolutionary new approach to
plasma cutting technology with IGBT internal chips. LONGEVITY® plasma cutters use the newest
technology available in the welding industry with the help of IGBT internal components allowing
us to push the standards of plasma cutting technology to the next level. With our industrial and
commercial plasma cutters, we are able to provide our customers with plasma cutters that will hold
up during industrial applications. By producing the units with inverter technology, we are able to
produce smaller and more efficient units. During the manufacturing process, we kept the
maintenance and repair in mind by enabling the internal components of the machine to be a simply
plug and operate circuitry enabling all mother boards to be simply replaced and swapped out if
warranty was ever an issue. The ForceCut™ series plasma cutters use special safety-redundant
circuitry with built in auto-protection and self-adjusting circuitry to keep the machine running at a
safe threshold. This helps protect the machine from over-voltage, power spikes, tip blowouts and
shorting
cutter. We are proud of our achievements in the welding industry, we are
thankful you have chosen to use the LONGEVITY® ForceCut™ series.
. We hope you enjoy your LONGEVITY® ForceCut™ series plasma
www.longevity-inc.com 3
Page 8
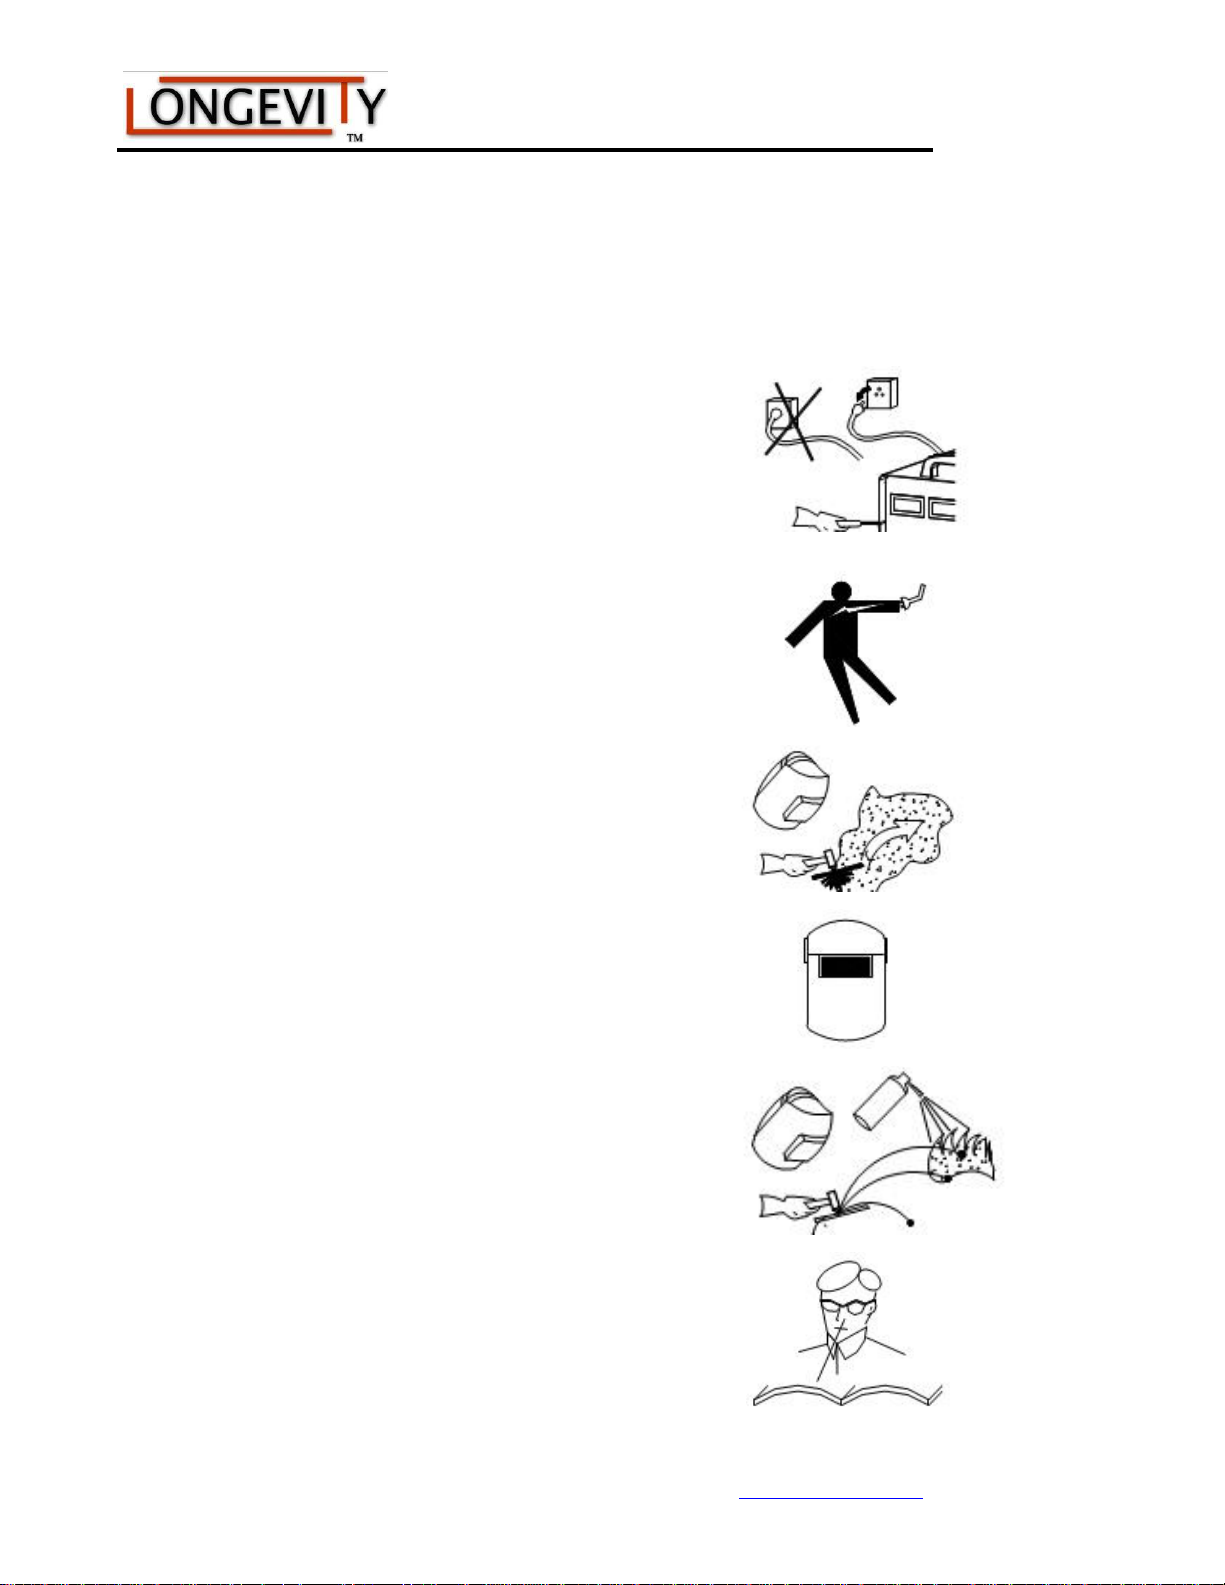
Welding and plasma cutting may be dangerous to the operator and to bystanders, if the
equipment is not operated properly. Welding or cutting must be performed in accordance
with all relevant safety regulations. Carefully read and understand this instruction manual
before installing and operating this equipment.
Changing function modes during welding may damage
equipment.
Before welding, disconnect the electrode-holder cable
from the equipment.
A circuit breaker is required to prevent electrical
overload of the equipment.
Only high quality welding tools should be used.
Electric Shock can be fatal.
Ensure that ground cable is connected in accordance with
applicable safety codes.
Never touch electrodes, wires, or circuit components with
bare hands. Wear dry welding gloves when welding.
The operator must be insulated from the work piece.
Smoke and gas can be harmful to health.
Ensure that the working area is well ventilated.
Avoid breathing smoke and gas generated during the
welding process.
Arc-light emission can be harmful to eyes and skin.
Always wear a welding helmet, anti-radiation glass, and
work clothes while welding.
Ensure that people in or near the working area are
protected.
Welding splash is a fire hazard.
Keep flammable material away from the work place.
Keep a fire extinguisher nearby, and have all personnel
trained in it’s use.
Surface noise generated while welding or cutting can be
harmful to hearing.
In the event of a machine fault.
Refer to this instruction manual.
If the fault cannot be determined, contact your local
dealer or supplier for assistance.
Warning
PLASMA CUTTERS www.LWELD.com
4 www.longevity-inc.com
Page 9
Plasma Cutters www.LWELD.com
Safety Tips
Consider the following tips to ensure safe operation of your welding/cutting
equipment:
Ensure that this welding equipment is installed in an area free of corrosive
chemical gases, flammable gases or materials, and explosive chemicals.
The area should contain little dust, and have a humidity of no more than 80%.
Operate the welding equipment in an area sheltered from direct sunlight and
precipitation. Work area temperature should be maintained at -10C to +40C;
If, because of an overload, the machine suddenly stops, and it is necessary to
restart it, leave the internal fan operating to lower the inside temperature.
Always wear protective clothing and a welding mask to protect your skin.
Wear safety goggles designed to darken the arc generated by your machine.
Wear suitable noise protection to protect your hearing.
Ensure that machine is grounded through the power cord or on the machine case.
Never operate the machine in bare feet or on a wet floor.
Never switch the machine off while it’s in use. Doing so will damage the internal
circuitry.
Ensure that your circuit breaker is rated to handle the current requirements of
your machine.
Use a UL approved receptacles and plugs with your machine. Never hard wire
the machine to main power.
Work in a well ventilated area to avoid smoke. Keep your head out of the smoke.
Ensure that air is flowing away from you to avoid inhaling smoke.
Ensure proper ventilation through the machine’s louvers. Maintain a distance
least 12 inches between this cutting equipment and any other objects in the
of at
work area.
Use a screen or curtain designed to keep passers by from viewing the arc.
The arc spray and metal spray from machine use may cause nearby fires. Use
caution.
If, after reviewing this manual, you have any problems in setting up or operating
your machine, contact us at help@LONGEVITY®-inc.com.
www.longevity-inc.com 5
Page 10
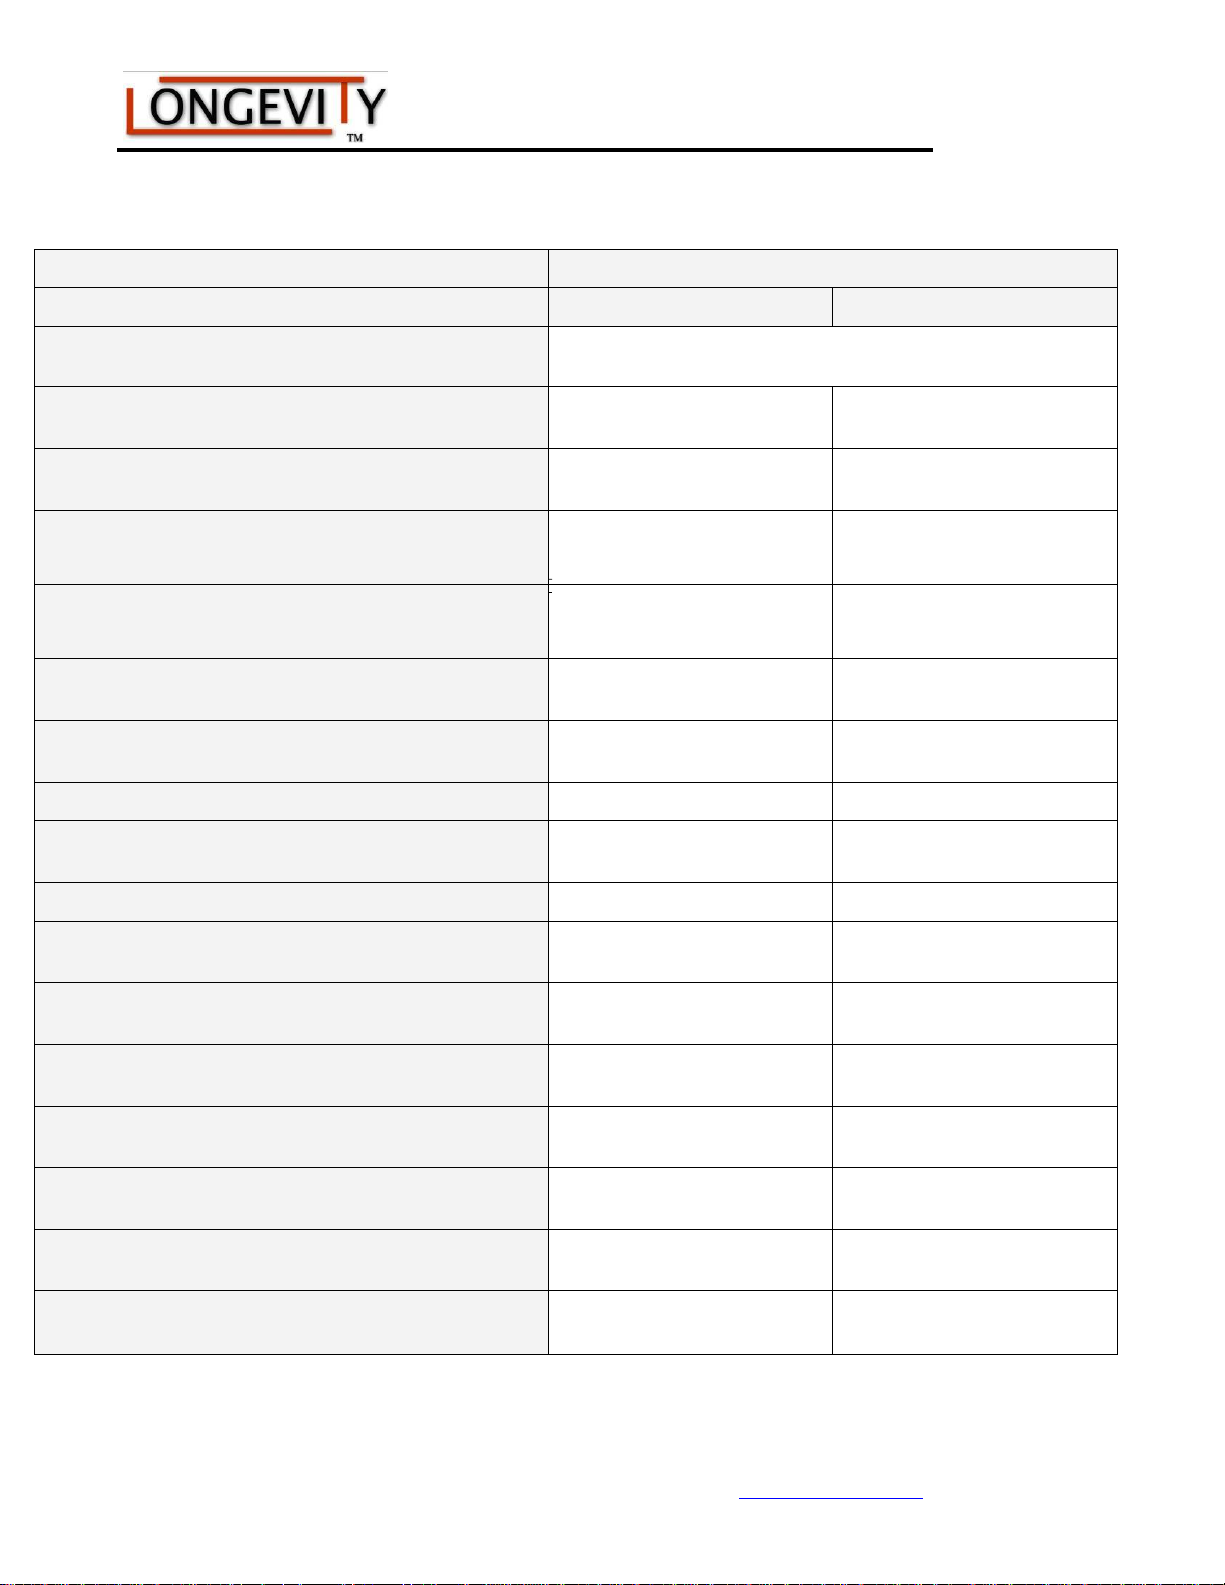
Type
Parameter
ForceCut 60i
ForceCut 80i
Input Voltage (V)
Single Phase 220/230/240V
Cup Capacity max/sev (in.)
Up to 1 ¼”
Up to 1 5/8”
Input Current (Amp)
50
70
Output Current (Amps)
60
80
No-load Voltage (V)
200v
200v
Current Range (Amp)
20-60
20-80
Rated Duty Cycle (%)
60
60
Efficiency
85
85
Power Factor (Cos0)
0.93
0.93
Insulation Class
B
B
Protection Class
IP21
IP21
Arc Starting
HF Continuous Pilot Arc
HF Continuous Pilot Arc
Suggest Air Pressure (psi)
75-80
75-80
Suggested Air Volume (cfm)
4.0
4.0
Adjustable Post Flow Time (Seconds)
2-10
2-10
Machine Weight (lbs)
42
48
Size LxWxH (inches)
21 x 9 x 15
24 x 11 x 17
PLASMA CUTTERS www.LWELD.com
Specifications and Ratings
6 www.longevity-inc.com
Page 11
Plasma Cutters www.LWELD.com
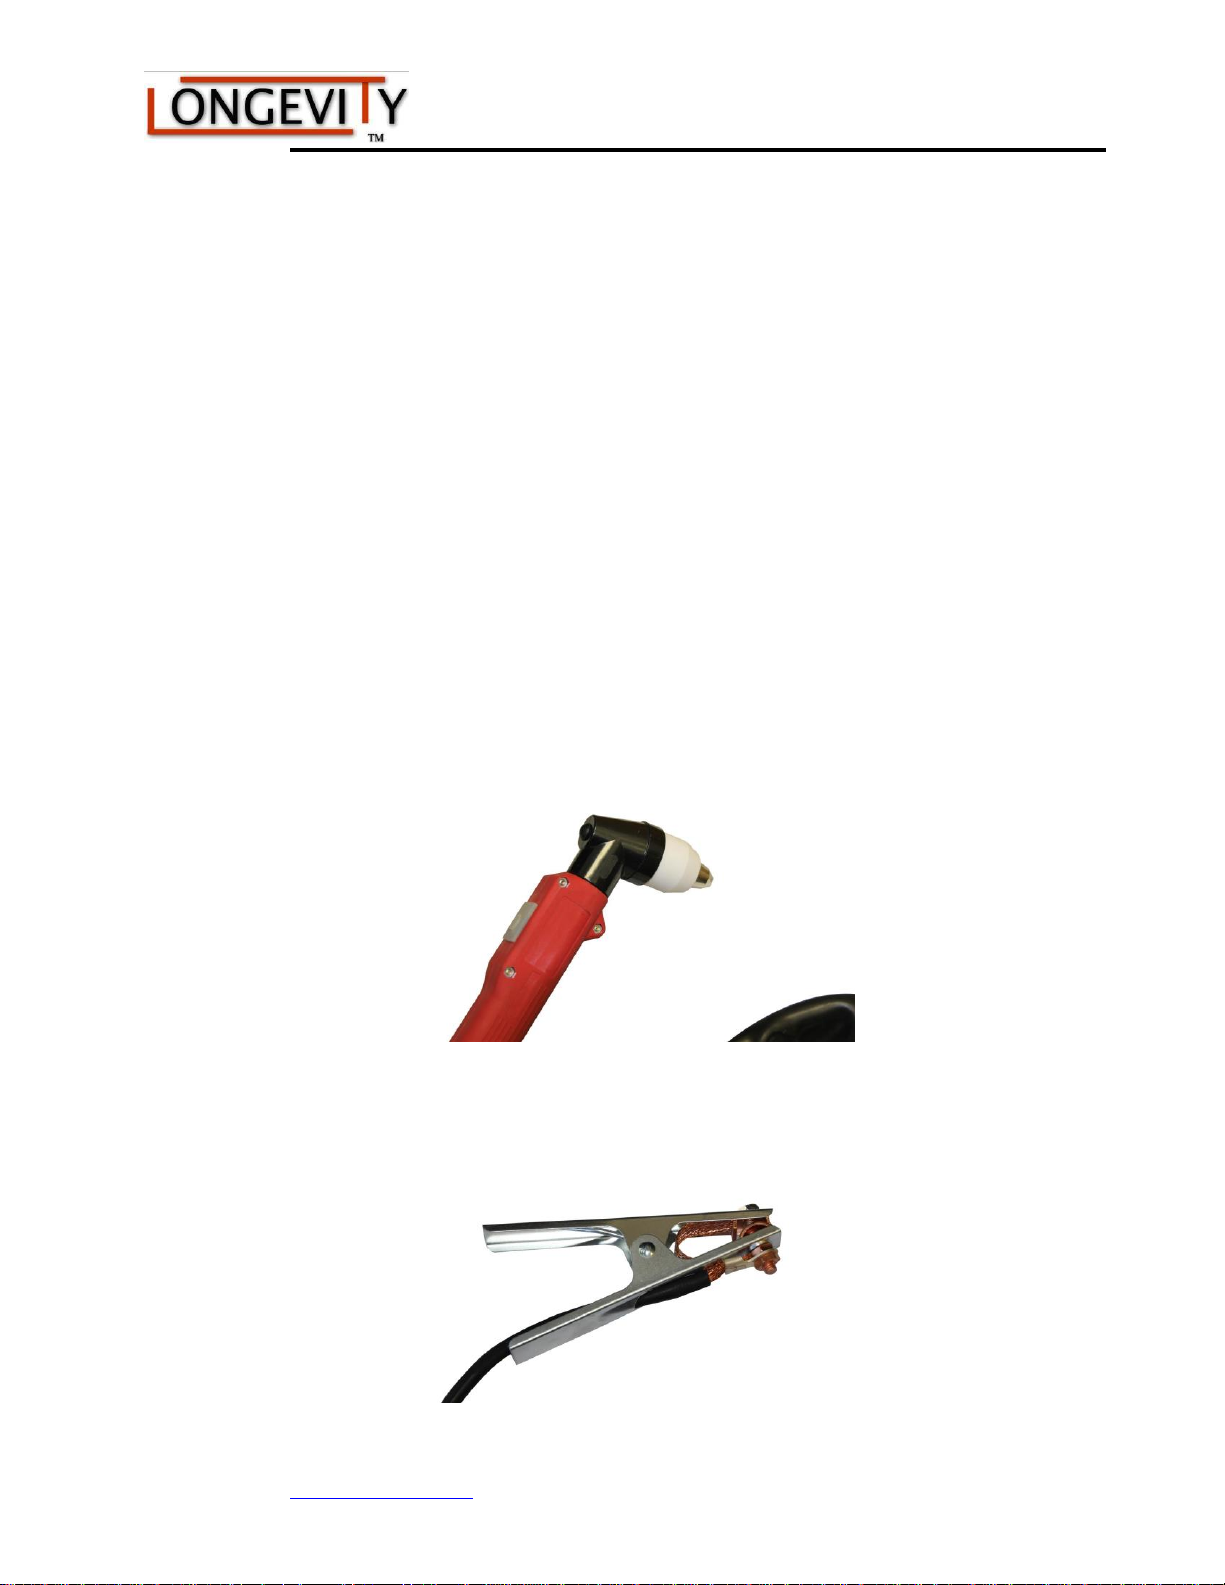
What’s Included:
Main Unit
Cutting Torch
(Ground) Earth Clamp
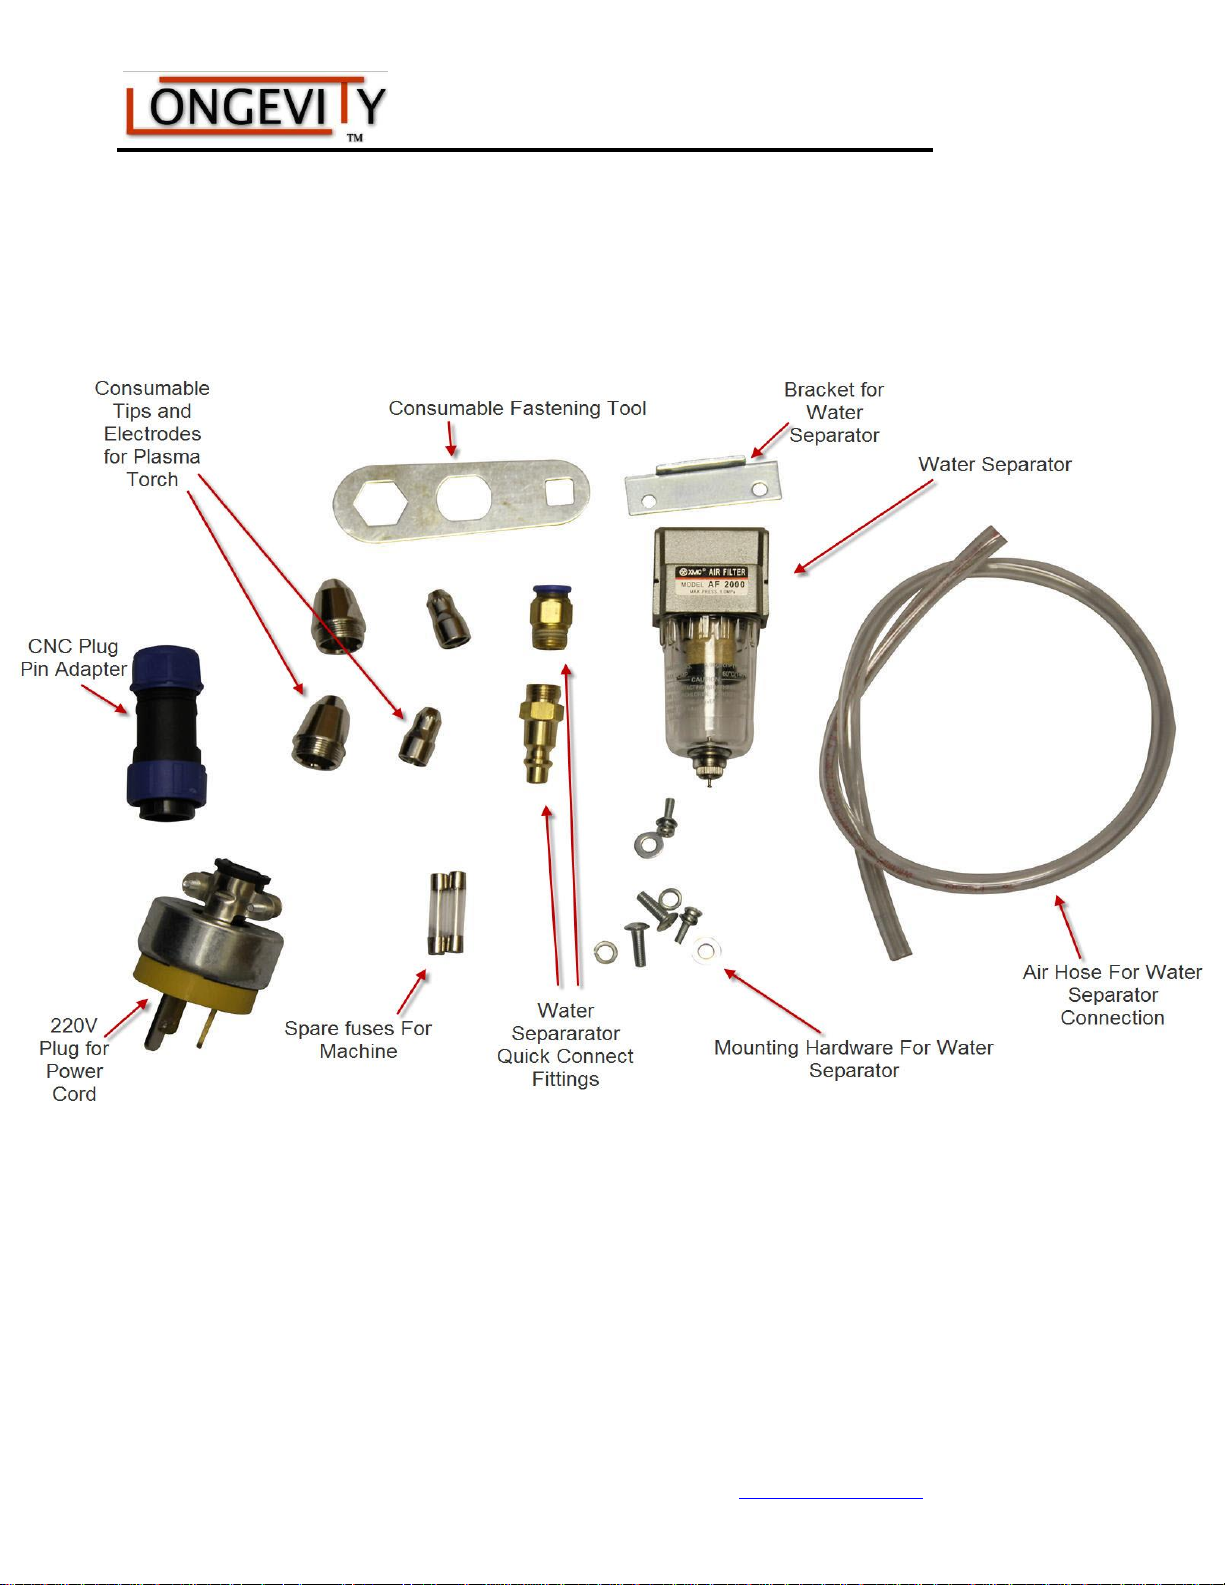
Water Separator and Bracket
Air Hose
Consumables: 2 piece tips, 2 piece electrodes, and 2 piece shield cups
Power Plug
CNC Plug Pin Adapter
Pictures of Accessories: (Note: 60i accessories
pictured)
Plasma Torch
(Note: Torch will vary by model)
Ground Clamp
www.longevity-inc.com 7
Page 12
PLASMA CUTTERS www.LWELD.com
60i and 80i Included Accessories:
8 www.longevity-inc.com
Page 13
Plasma Cutters www.LWELD.com
Installation and Setup Instructions:
The item numbers referenced in the following paragraphs, refer to the numbered
parts display in the diagrams shown below. LONGEVITY® has an instructional
setup installation video on our website at www.longevity-inc.com, which we ask that
you view prior installing the unit. The video shows the complete assembly of the
machine. The video is located in the Resources section of the website under manuals
and installation/set-up videos.
The LONGEVITY® ForceCut 60I and 80I are both 220v 1 phase units.
Connecting the electrical plug to the unit
Connecting the power plug to the unit is important. Please view the proper
connection instructions below:
Wiring Introduction for 220 Volt
Danger: Read this manual completely before having your electrician attempt to wire
up or connect your machine to an electrical power source. LONGEVITY® units
should be wired by a certified electrician to insure your safety and a proper
110/220v plug match at your operating facility. Remember 220v plugs come with 3
or 4 prongs on them. Have the electrician check your existing receptacle.
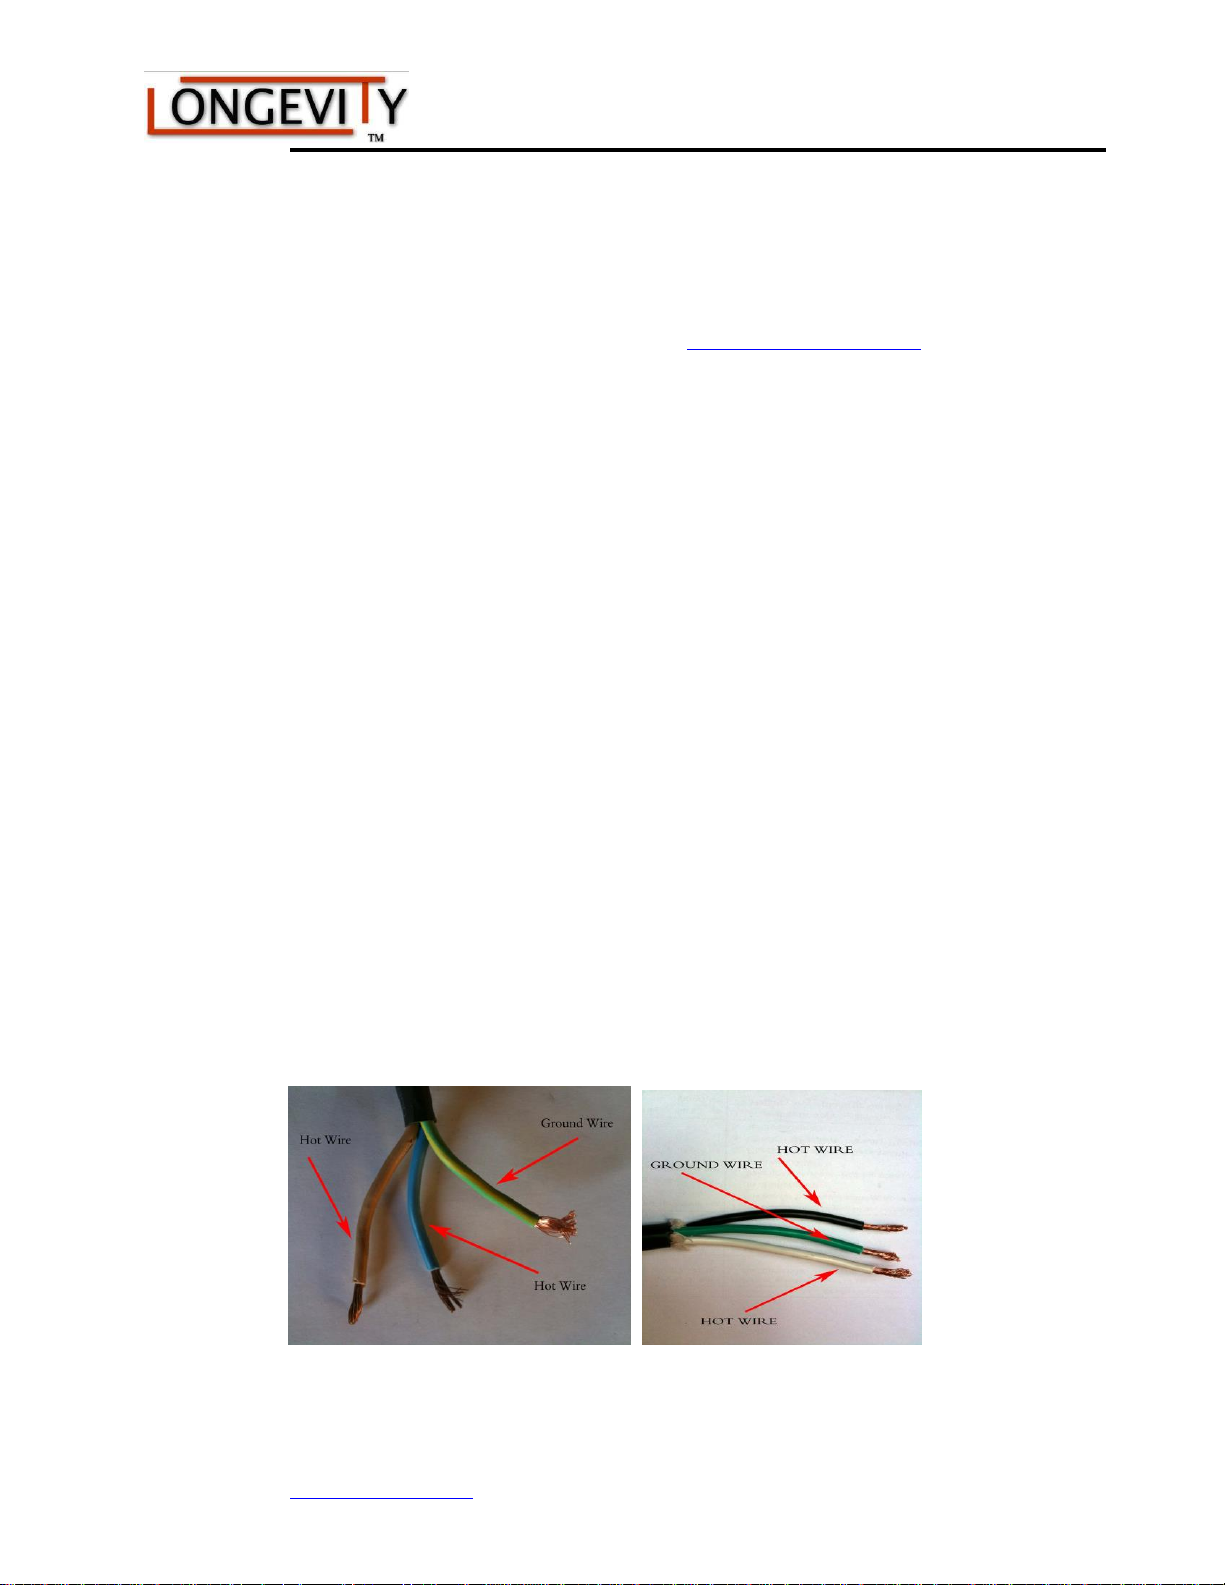
Note: The power cord on single-phase machines has one ground wire and two hot
wires when connecting to 220vac. Connecting these wires properly is extremely
important. Improperly connected wires will void the warranty, affect personnel
safety, and possibly damage your machine and electrical power outlet.
www.longevity-inc.com 9
Page 14
PLASMA CUTTERS www.LWELD.com
Identifying
Caution: The machine may appear to operate with an incorrectly connected ground
wire, but it will not operate properly. Selecting the correct ground wire is important
for proper machine operation and personnel safety.
Ground wires on LONGEVITY® Welding machines are usually one of the following
colors:
The ground wire is a dark green with a yellow stripe. The wire may also be just
SOLID GREEN.
Clean the ends of the wires to more easily distinguish the colors. The best and safest
way to determine which wire is ground is to measure the resistance between the
machine chassis and the selected wire, using an ohmmeter. Another method is to
check the continuity between the chassis and the wire, using a continuity meter. If
the selected wire is ground, the connection between the chassis and the wire will
cause the meter to illuminate. If, for any reason, you cannot visually detect the
ground wire or do not feel comfortable with your selection, ask an electrician for
help.
Identifying
For 220vac service, both the brown and blue wire are positive wires. As you may
know, 220vac features two hot wires. If you are wiring to 220vac, your blue and
brown wires are both hot. The green with yellow or SOLID GREEN is the
ground. Remember, any hot wire can be attached to either hot leg on the plug.
Note: Hot Wires May also be WHITE and BLACK if a GREEN WIRE is one of
the three wires. Therefore, GREEN is ALWAYS GROUND.
NOTE: LONGEVITY® recommends a 30 AMP breaker.
the Ground wire
the hot wire
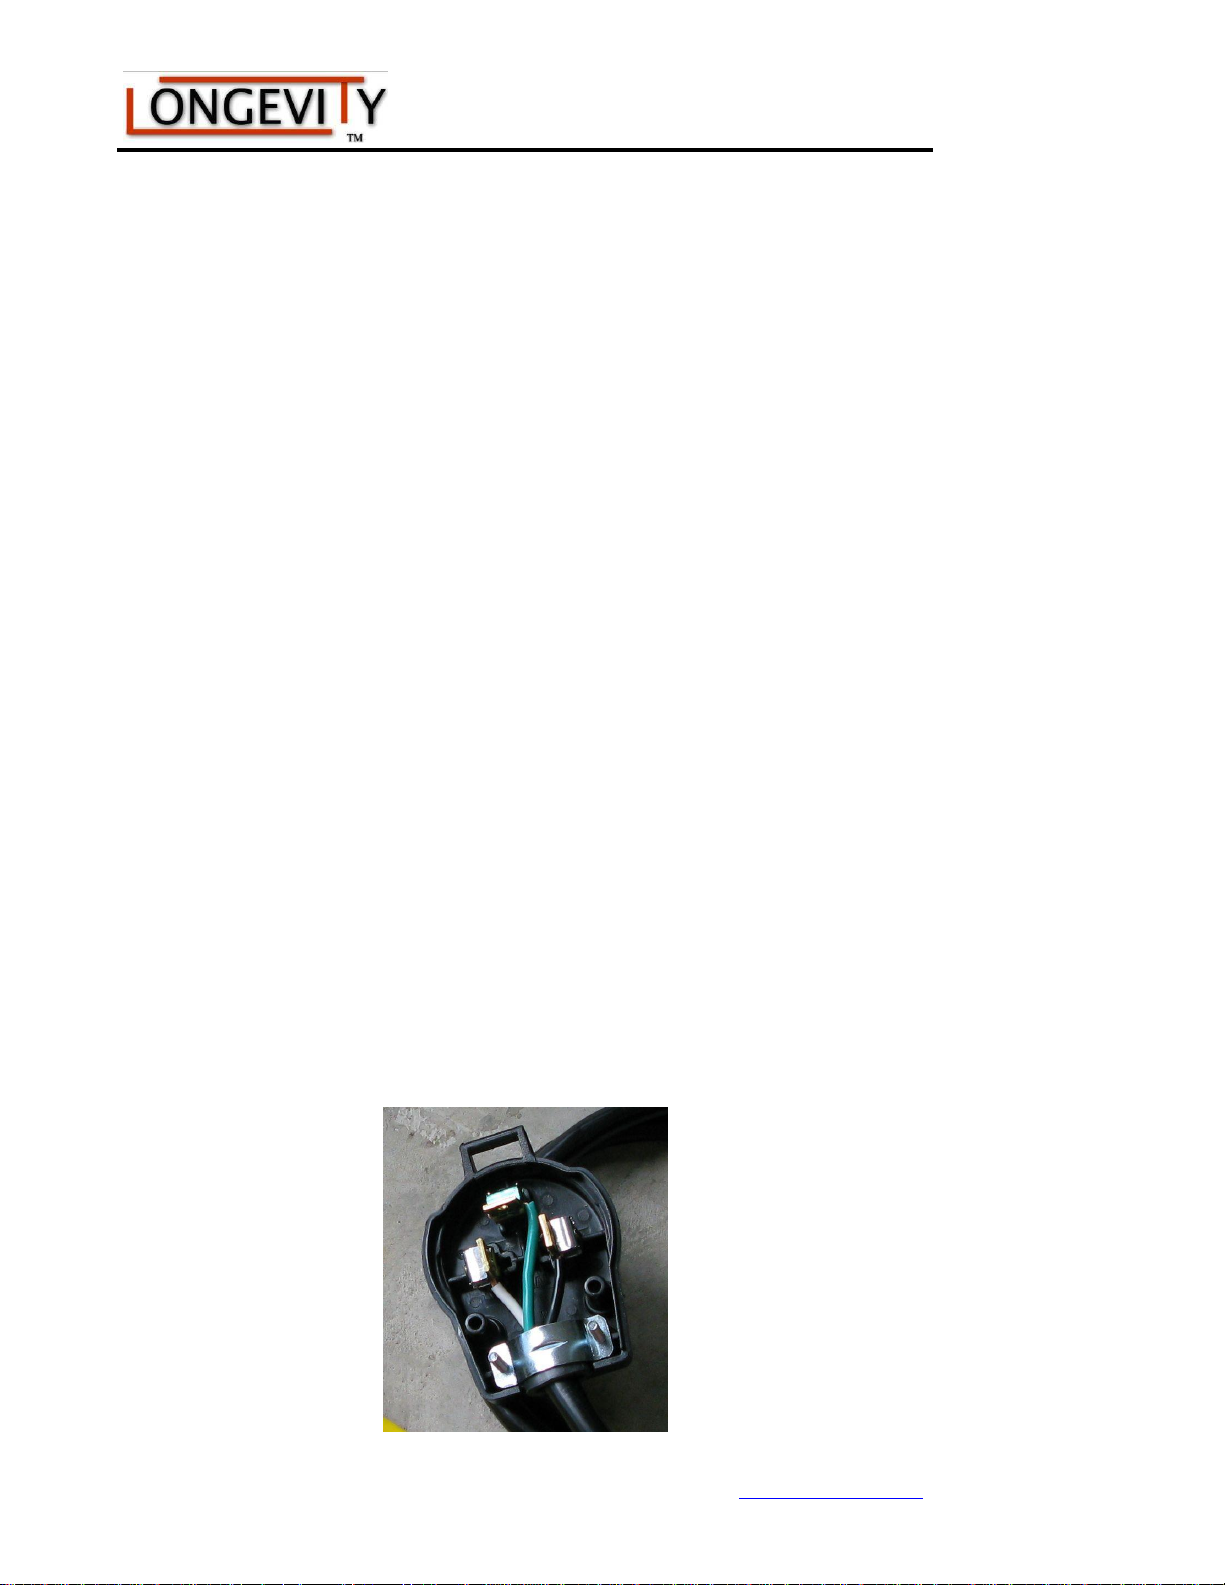
Finished Plug:
10 www.longevity-inc.com
Page 15
Plasma Cutters www.LWELD.com
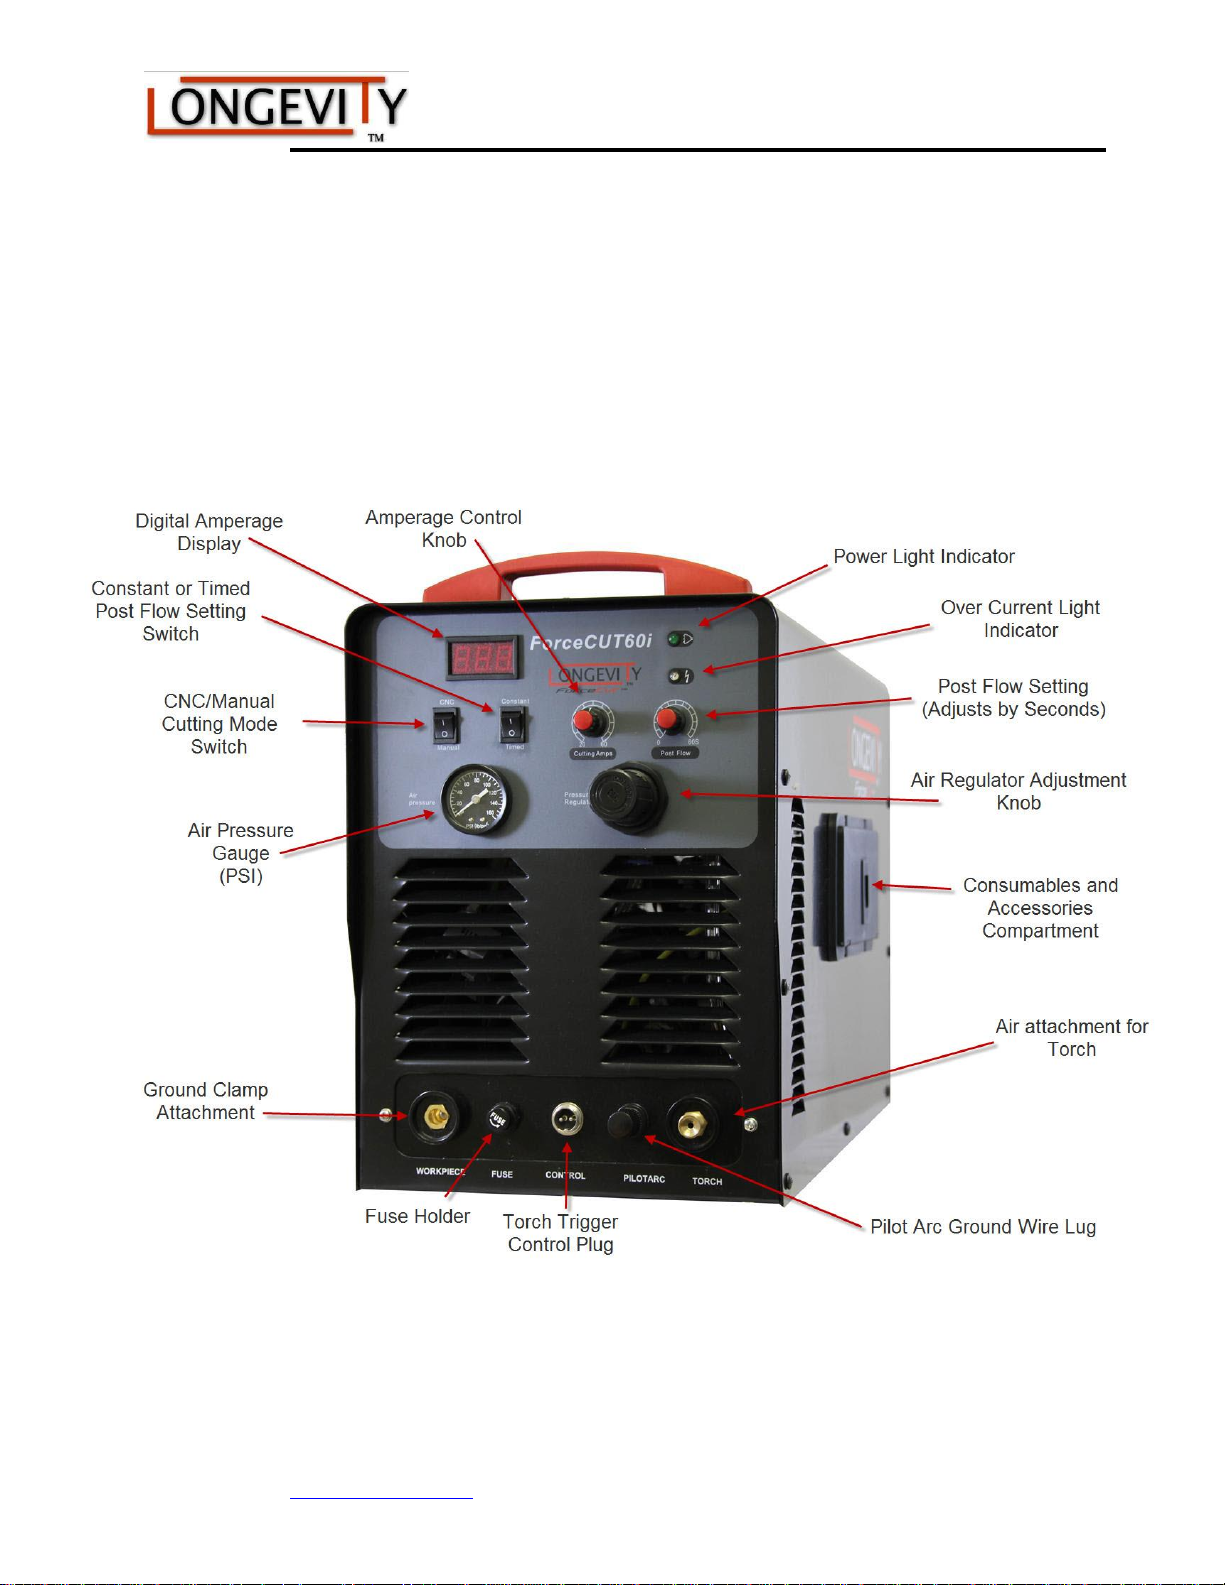
Basic Diagram Pictured Model ForceCut™
60i (Note: Both 60i and 80i models have
the same connections)
www.longevity-inc.com 11
Page 16
PLASMA CUTTERS www.LWELD.com
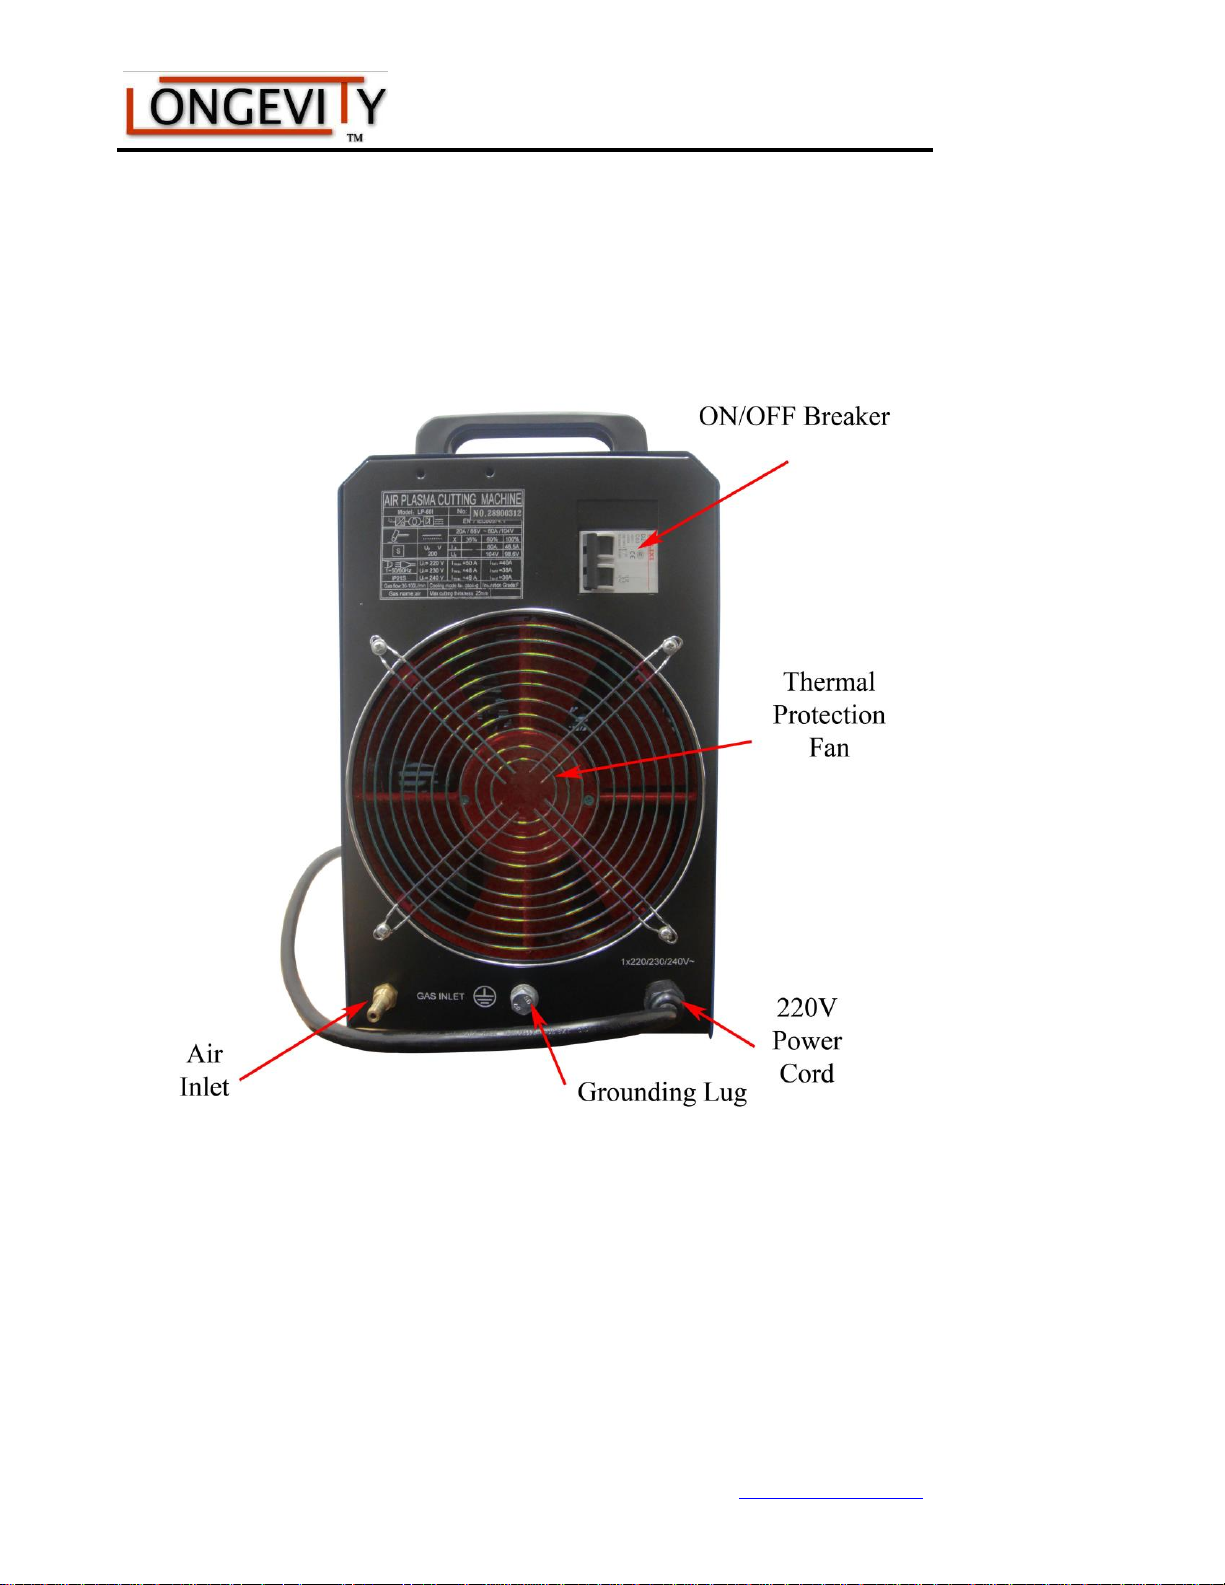
Rear View (Pictured ForceCut™ 60i
Plasma Cutter)
12 www.longevity-inc.com
Page 17
Plasma Cutters www.LWELD.com
Main Unit Knob/Button Functions/Inlets:
1. On/Off Breaker or Switch: Either breaker or switch located on the back or front of the
unit will control the unit to be turned on or off.
2. Power Indicator : Shows unit is powered on. Indicator is present in some models with
a green LED bulb.
3. O.C. Over Current Light: Illuminates when the duty cycle has been exceeded or the
machine has overheated due to improper ventilation. Discontinue use until lamp goes
out. Allow the fan to continue to run. Once lamp goes out, you may resume using the
unit.
4. Digital Display: Displays the approximate amount of amperage set to on the unit.
5. Gas (Air) Test/Cutting: This mode allows you to test air pressure and release air
through the torch. Selecting Gas (Air) Test, you should have air passing through the
torch as long as the compressor is on. Cutting mode allows you to use the plasma cutter
normally.
6. AMP Adjustment Knob: Adjusts the amount of amps to desired AMP setting.
7. Ground Clamp Connector (+): Location of ground clamp to be plugged in and ran to
the workpiece.
8. Torch Remote Connector: 2 or 7 pin torch connector plugs here to activate the torch
relay once the trigger is pressed on the torch.
9. Torch Connector: Connect torch for air to pass through the unit and generate the arc
at the torch tip.
10. Pilot Arc Torch Connector: Connect the torch pilot arc wire coming from the torch to
this knob for proper arching.
11. Torch Air Outlet: This is only used with specific torches that require water cooling.
Your unit does not come with this feature as it is not required.
12. Air Regulator Pressure Gauge: Shows the amount of pressure at the torch in PSI.
13. Pressure Regulator Adjustment Knob: Adjust the amount of pressure at the unit. Pull
the knob towards you to unlock, turn clockwise for more pressure and counter
clockwise for less pressure. Once the desired pressure is reached, pop the knob back in
place to lock it in place.
14. Thermal Protection Fan: Cools your unit during operation. Fan should be operating
once the power is turned on and the unit power indicator is lit.
15. 220v Power Cord: Attach the power cord to the wall outlet for unit power. Required
30amp breaker on 220v side.
16. Ground Lug: An additional safety grounding lug. You can earth this wire or properly
ground it to your electricians specifications. Grounding the unit and yourself during
cutting is extremely important
17. Air Inlet: Attach air compressor hose to the air inlet here.
www.longevity-inc.com 13
Page 18
PLASMA CUTTERS www.LWELD.com
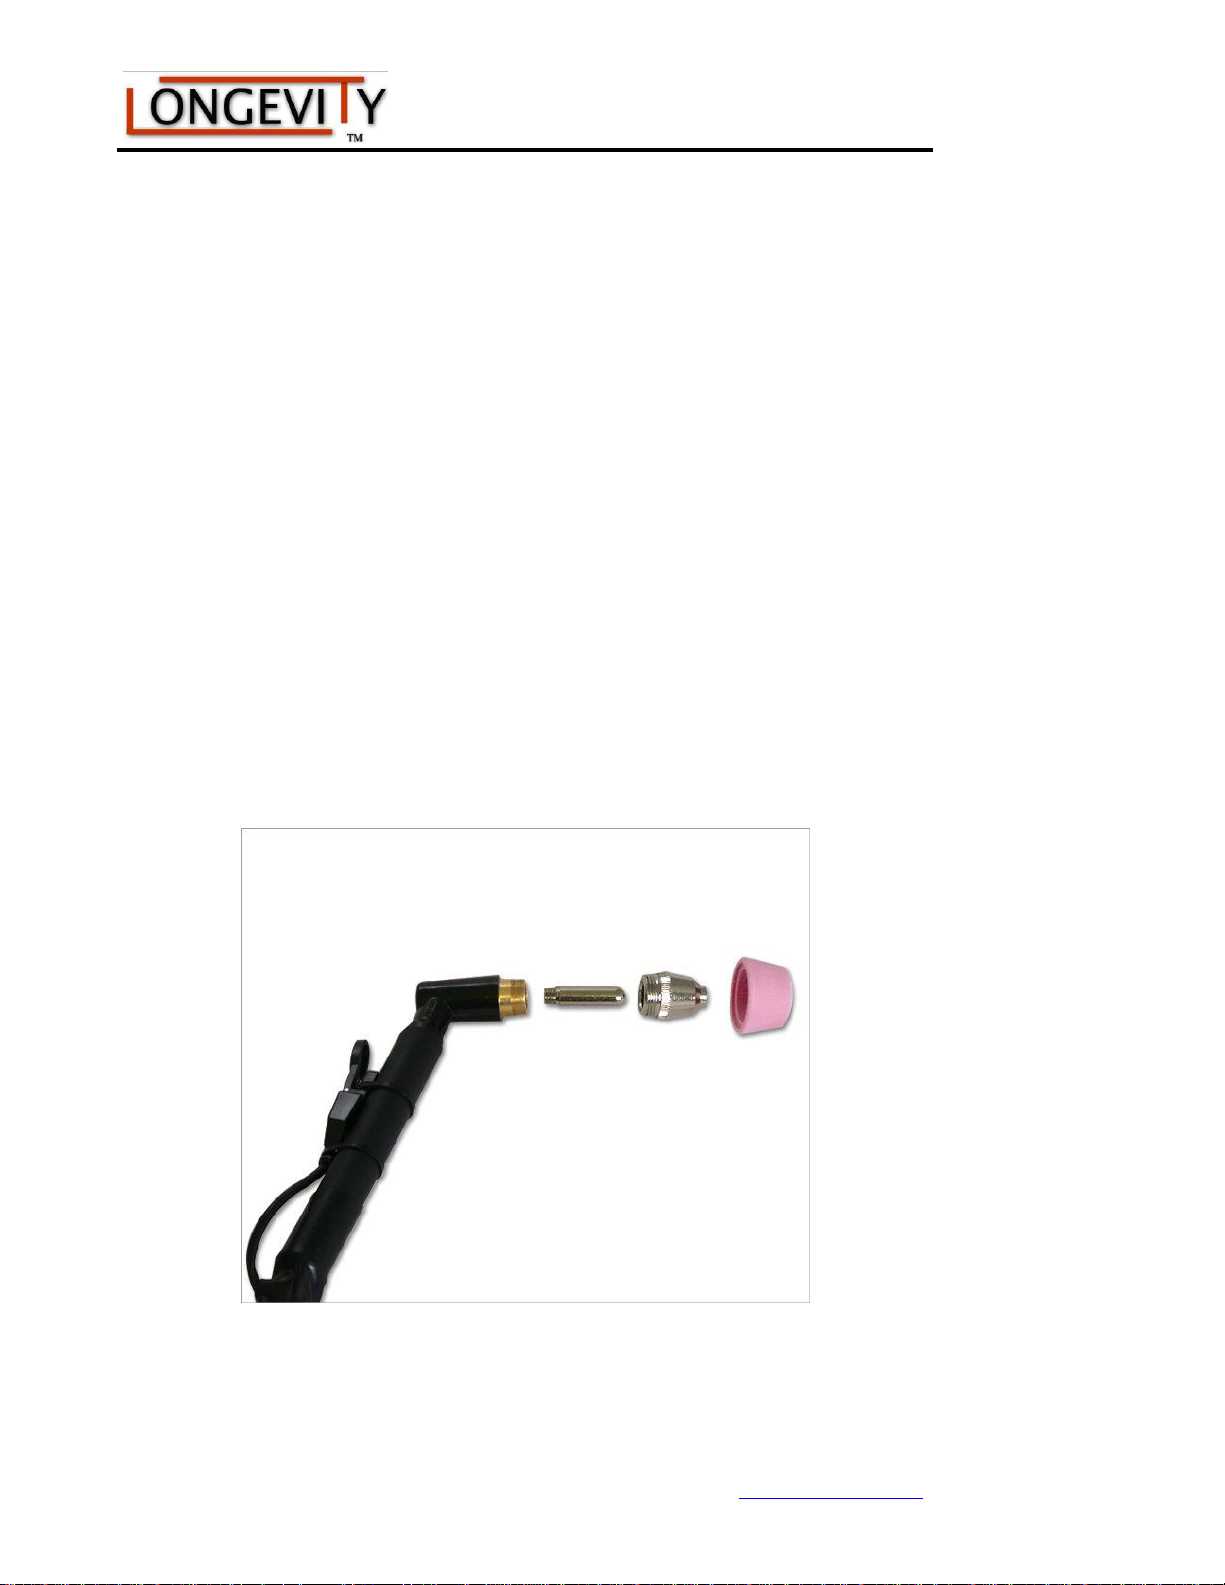
Plasma Torch Assembly:
The plasma cutter torch handle is made of fire and heat resistant materials. Avoid
dropping the torch or striking anything with it. For convenience and ease of use, the
torch’s ON/OFF switch can be positioned on the top, the side, or the bottom of the
torch body.
Assembly for the ForceCut™ 60i model.
Assemble the consumables as pictured above, and described below.
1. Insert the electrode.
2. Place the copper tip over the electrode, ensuring that is seated flat.
3. Secure all parts into place by turning the pink ceramic cup clockwise until it
is snug. Do not over tighten.
4. If your unit comes with a torch space, place spacer into the groove of the
ceramic tip.
5. Remember to properly plug the torch into the unit including the Pilot Arc
wire.
The torch consumables are now successfully assembled.
14 www.longevity-inc.com
Page 19
Plasma Cutters www.LWELD.com
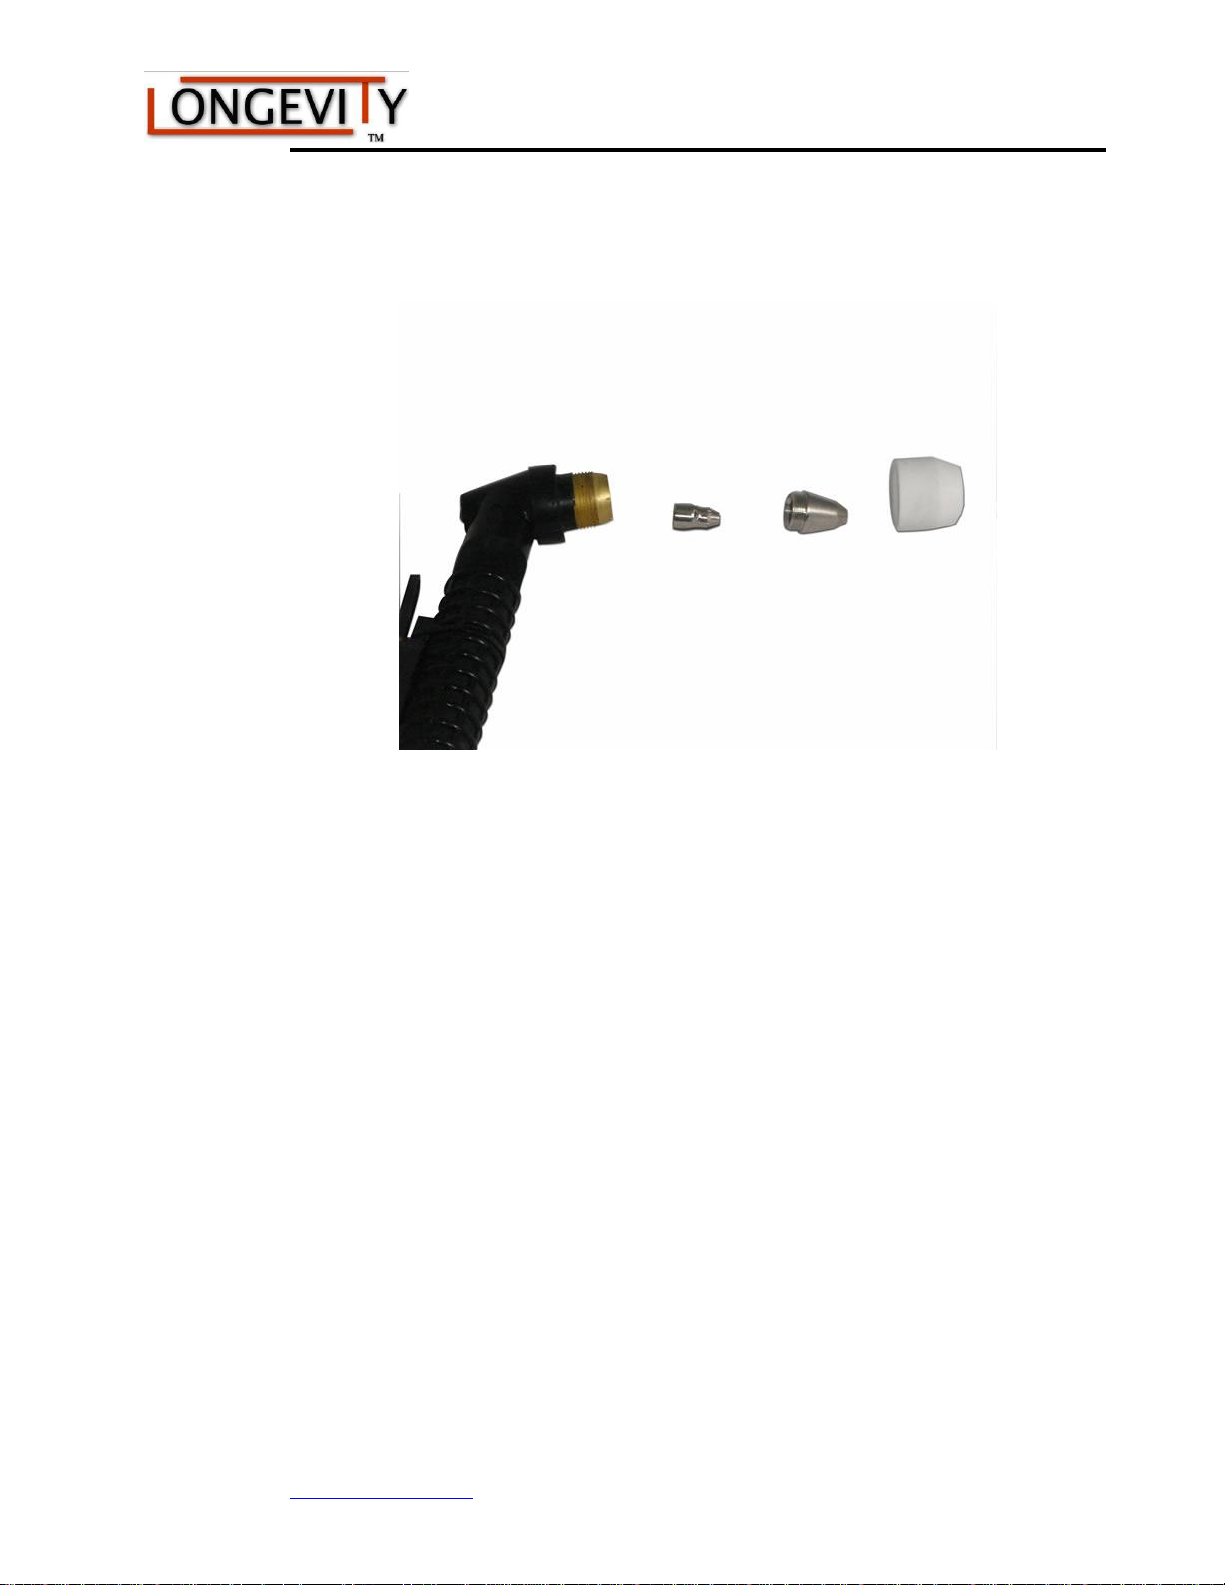
Assembly of ForceCut 80i Plasma Cutter
Assemble the consumables as pictured above, and described below.
1. Insert the electrode.
2. Place the copper tip over the electrode ensuring that is seated flat.
3. Secure all parts into place by turning the ceramic cup clockwise until it is
snug. Do not over tighten.
4. If your unit comes with a torch spacer, you can properly attach it to your
torch.
5. Remember to properly secure all connections of the torch to the unit.
The torch consumables are now successfully assembled.
www.longevity-inc.com 15
Page 20
7
PLASMA CUTTERS www.LWELD.com
Basic Operation
1. Ensure that all cables are connected to the machine.
2. Ensure that the machine’s OFF/ON switch is set to OFF, and plug the machine
into the electrical outlet.
3. Connect the air compressor supply line to the air input side on the unit.
4. Turn the ON/OFF switch to ON. The cooling fans should operate and the ON
indicator LED or power switch (if applicable) should illuminate.
5. Clean the contact point on the work piece to ensure a good electrical connection.
Ensure that no rust of paint is present that could create an open circuit.
6. Connect the ground clamp to the work piece to be cut.
7. Connect the torch to the unit properly.
8. With the pilot arc knob connected, you should get a full continuous arc when the
trigger on the torch is pressed.
9. Depress the button on your torch to start the arc and begin cutting.
10. You can test the air to insure that is it properly flowing by selecting Gas (Air)
Test. Air will pass through the torch.
11. If necessary remove slag from the under part of the cut using a grinder or chisel.
16 www.longevity-inc.com
Page 21
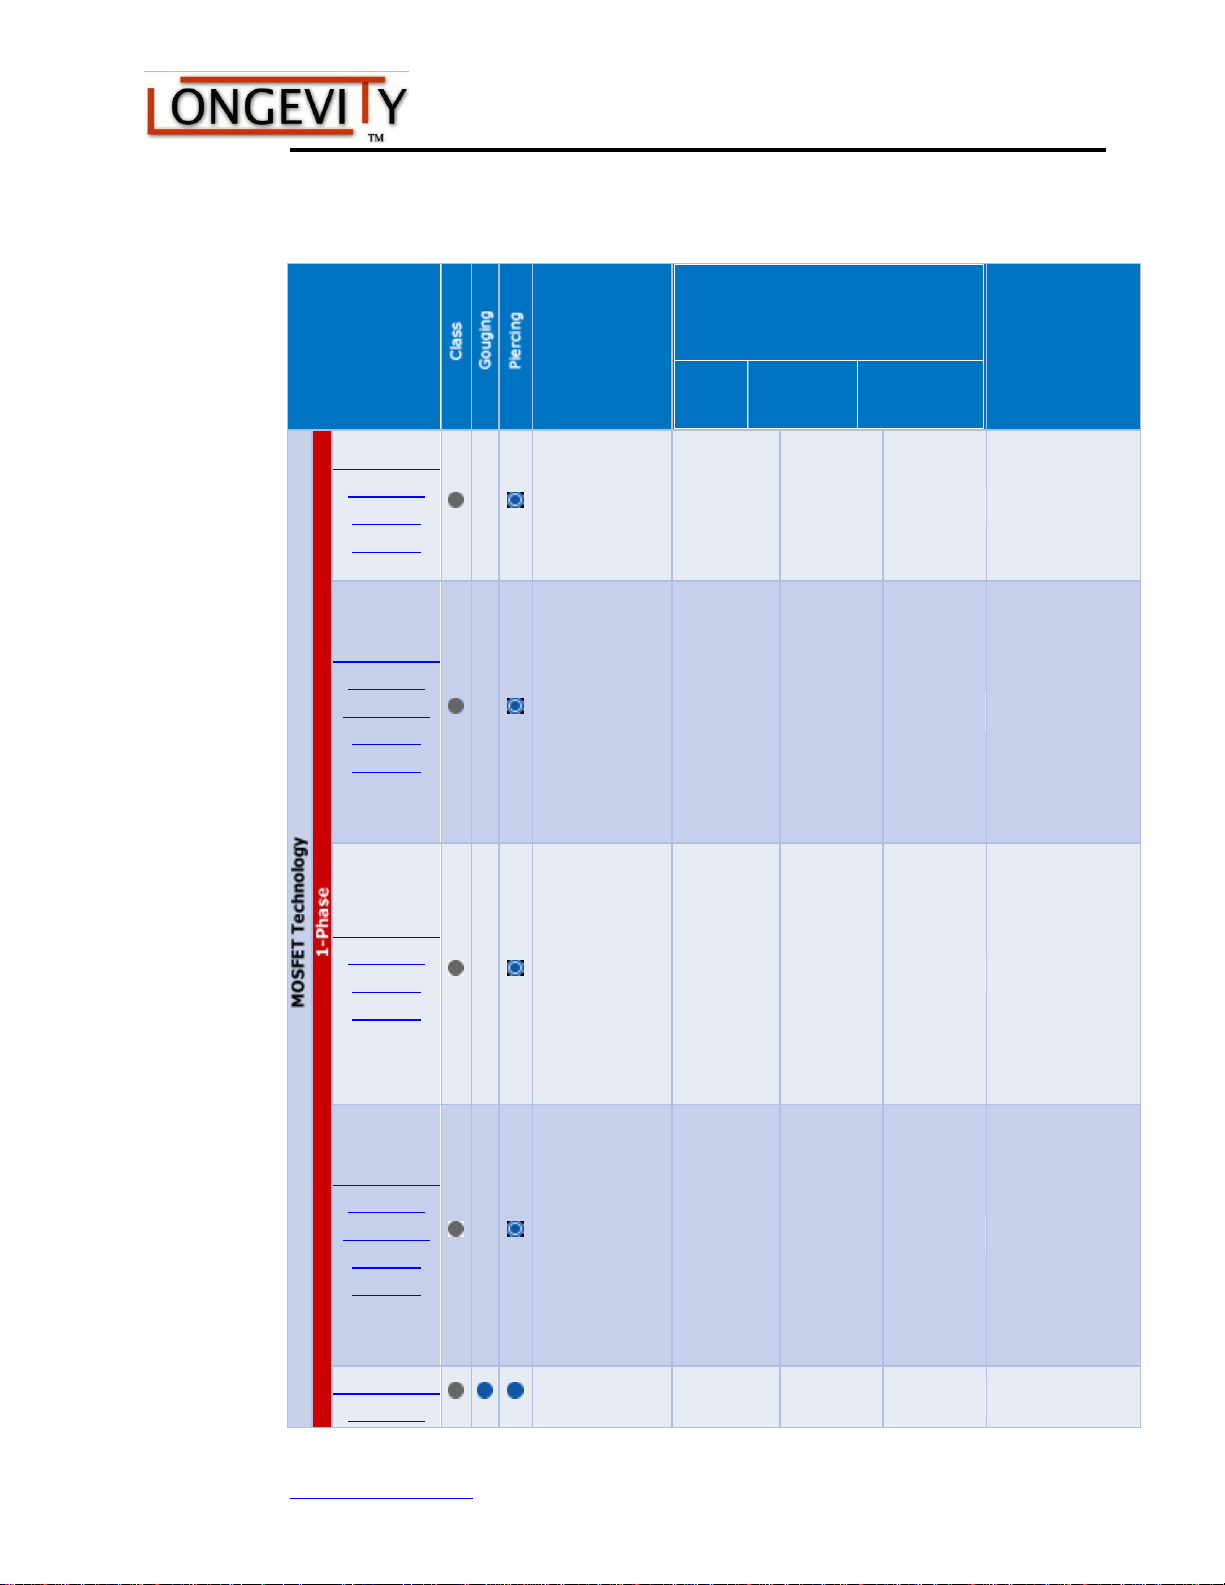
Plasma Cutters www.LWELD.com
Plasma Cutters
Rated Output
"Rated" Cutting Thicknesses at
220 V (110V reduces power in
half)*
Mild
Steel
Stainless
Steel
Aluminum
Recommended
Generator
Power
ForceCut®
LP-40D
Plasma
Cutters
40 A at 60%
(230 V Input)
30 A at 60%
(110 V Input)
1/2 in
1/2 in
1/4 in
2500 watts
ForceCut®
LP-40D
Pilot Arc
Plasma
Cutters
40 A at 60%
or 30 A at
100% (230 V
Input)
30 A at 60%
or 25 A at
100% (110 V
Input)
1/2 in
1/2 in
1/4 in
4000 watts
ForceCut®
LP-50D
Plasma
Cutters
50 A at 60%
or 40 A at
100% (230 V
Input)
40 A at 60%
or 30 A at
100% (110 V
Input)
3/4 in
3/4 in
3/8 in
4000 watts
ForceCut®
LP-50D
Pilot Arc
Plasma
Cutters
50 A at 60%
or 40 A at
100% (230 V
Input)
40 A at 60%
or 30 A at
100% (110 V
Input)
3/4 in
3/4 in
3/8 in
4000 watts
ForceCut®
LP-60D
60 A @ 60%
Duty Cycle
1 in
1 in
1/2 in
10,000 watts
Summary Chart of Plasma Cutters:
www.longevity-inc.com 17
Page 22
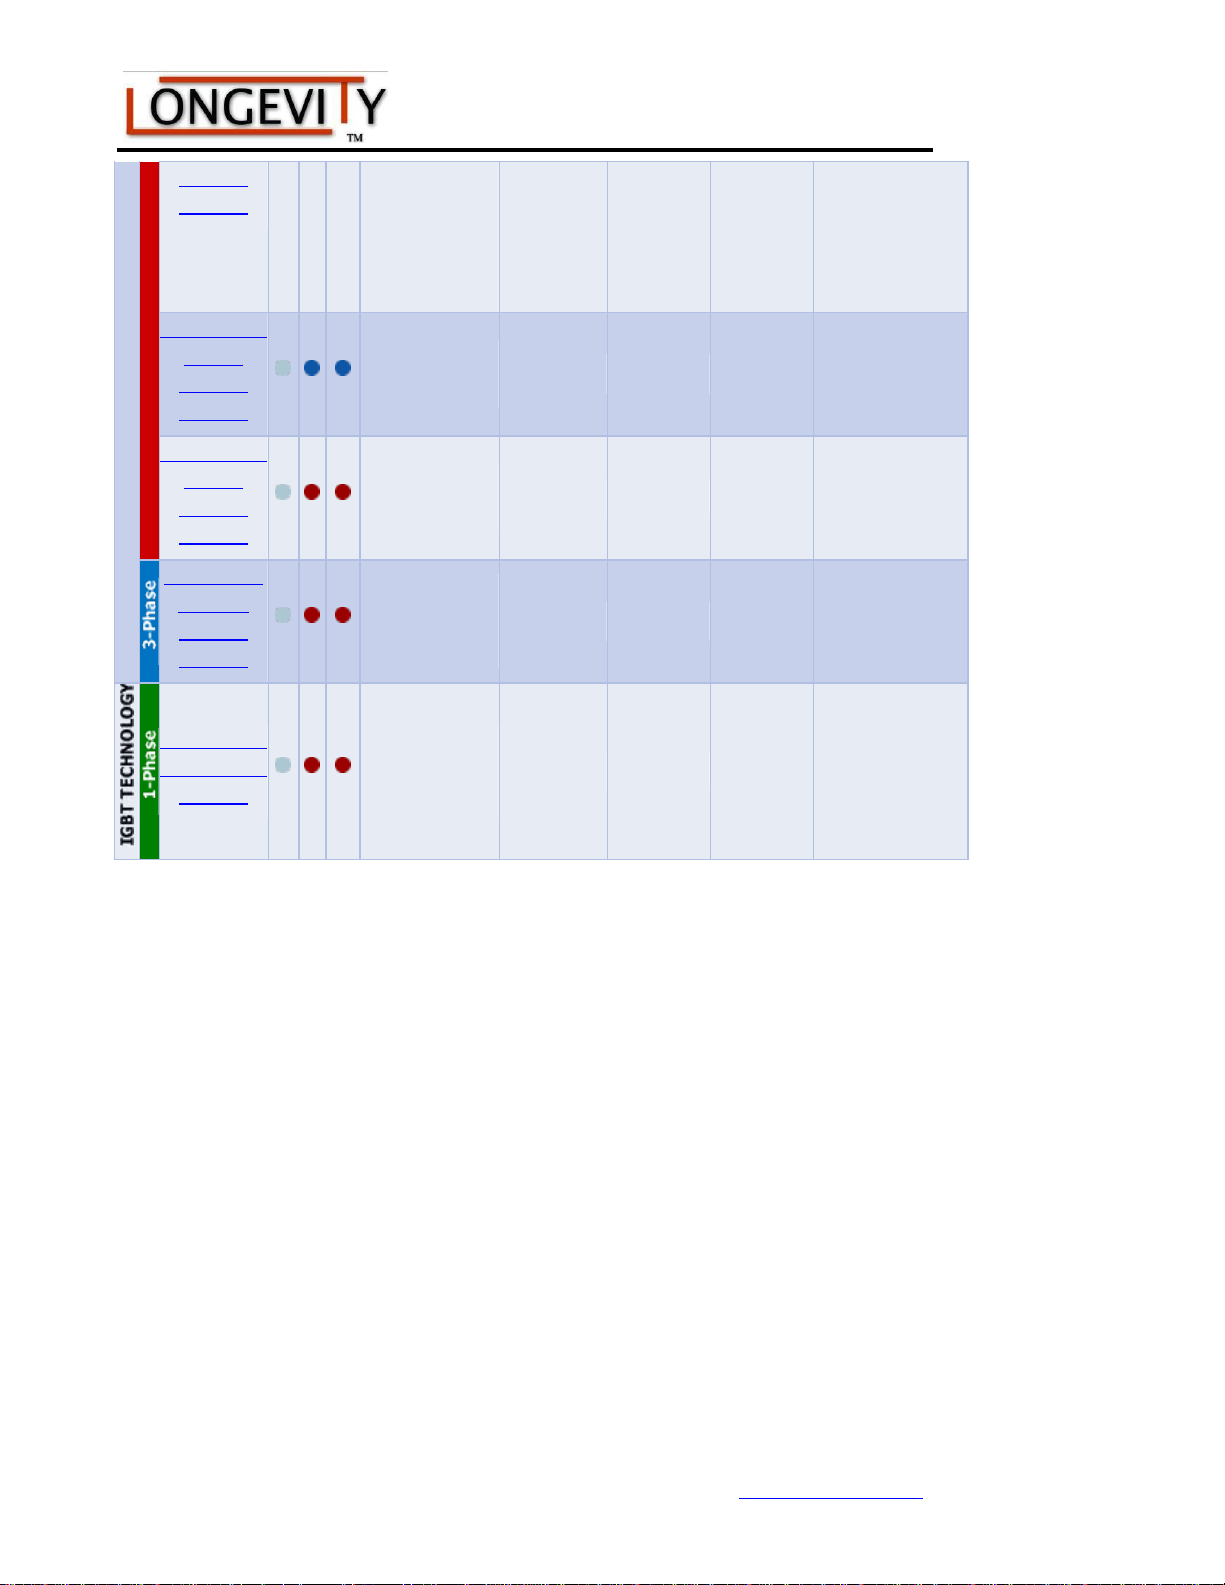
Plasma
Cutters
(230 V Input)
40 A @ 100%
Duty Cycle
(110 V Input)
ForceCut®
LP-70
Plasma
Cutters
70 A at 60%
(230 V Input)
1 1/4 in
1 1/4 in
5/8 in
8000 watts
ForceCut®
LP-80
Plasma
Cutters
80 A at 60%
(230 V Input)
1 1/2 in
1 1/2 in
3/4 in
9000 watts
MaxArc®
LP-100
Plasma
Cutters
100 A at 60%
(230 V Input
1- phase)
2 in
2 in
1/4 in
10,000 watts
ForceCut®
60I Plasma
Cutters
60 A @ 60%
Duty Cycle
(220 V Input)
1 1/4 in
1 1/4 in
3/4 in
6500 watts
PLASMA CUTTERS www.LWELD.com
18 www.longevity-inc.com
Page 23
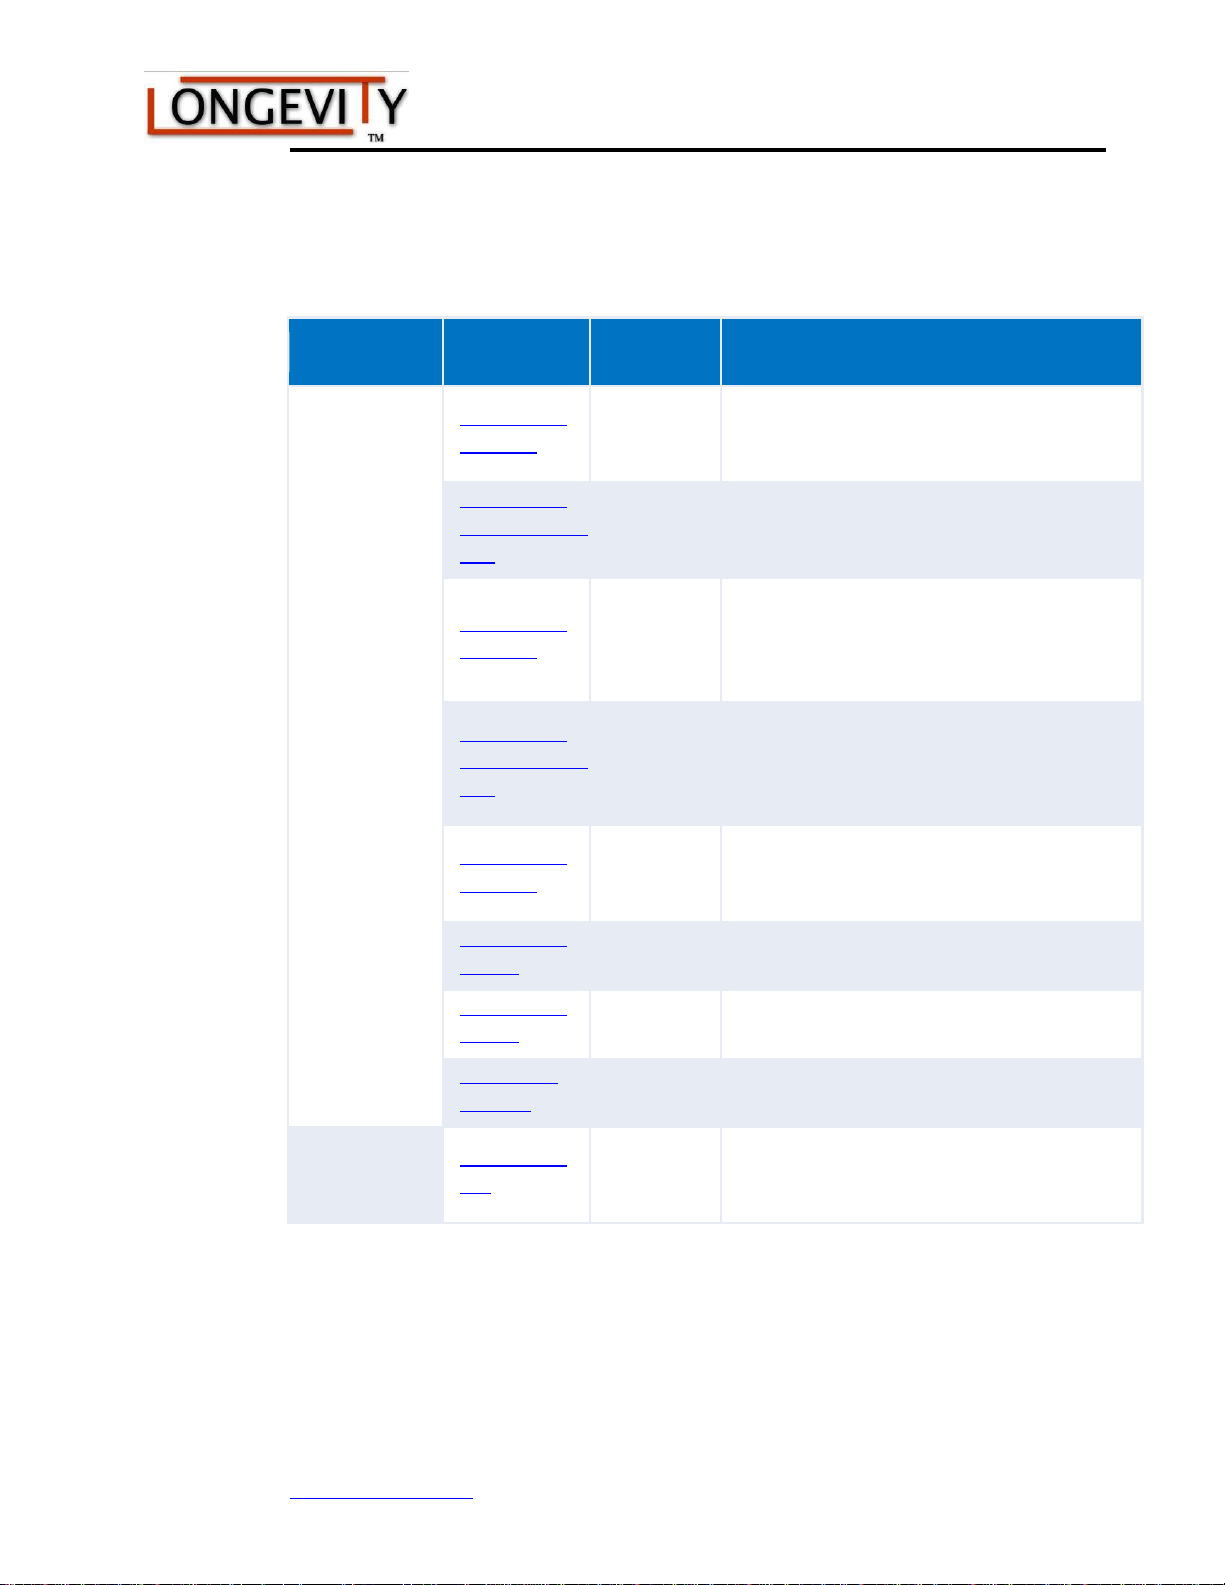
Plasma Cutters www.LWELD.com
Technology
Plasma Cutters
Product
Weight
Highlighted Features
MOSFET
Technology
ForceCut®
LP-40D
25 lbs (28 lbs
Boxed)
110/220 V Input, Portable, High
Frequency Start, Toshiba Mosfet
Technology
ForceCut®
LP-40D Pilot
Arc
25 lbs (28 lbs
Boxed)
Pilot Arc Starting Technology, 110/220
V Input, Portable, Toshiba Mosfet
Technology
ForceCut®
LP-50D
25 lbs (28 lbs
Boxed)
60% Duty at 50A & 100% Duty at 40A,
110/220 V Input, Portable, High
Frequency Start, Toshiba Mosfet
Technology
ForceCut®
LP-50D Pilot
Arc
25 lbs (28 lbs
Boxed)
Pilot Arc Starting Technology, 60% Duty
at 50A & 100% Duty at 40A, 110/220 V
Input, Portable, Toshiba Mosfet
Technology
ForceCut®
LP-60D
36 lbs (40 lbs
Boxed)
Powerful and Versatile! 110/220 V Input
with 1" Cut Capability, Toshiba Mosfet
Technology
ForceCut®
LP-70
38 lbs (45 lbs
Boxed)
Commercial Grade, Powerful, 220 V
Input, Toshiba Mosfet Technology
ForceCut®
LP-80
40 lbs (47 lbs
Boxed)
Most Powerful 1-Phase 220 V Input, 1
1/2 in Rated, Toshiba Mosfet Technology
MaxArc®
LP-100
74 lbs (90 lbs
Boxed)
Industrial Grade, 220 V Input 3-phase, 2
in Rated, Portable
IGBT
Technology
ForceCut®
60I
45 lbs (52 lbs
Boxed)
Commercial Plasma Cutter, Portable,
Industrial Grade, 220 V Input 1-Phase,
1.25" Cut Power
Features Chart of Plasma Cutters:
www.longevity-inc.com 19
Page 24
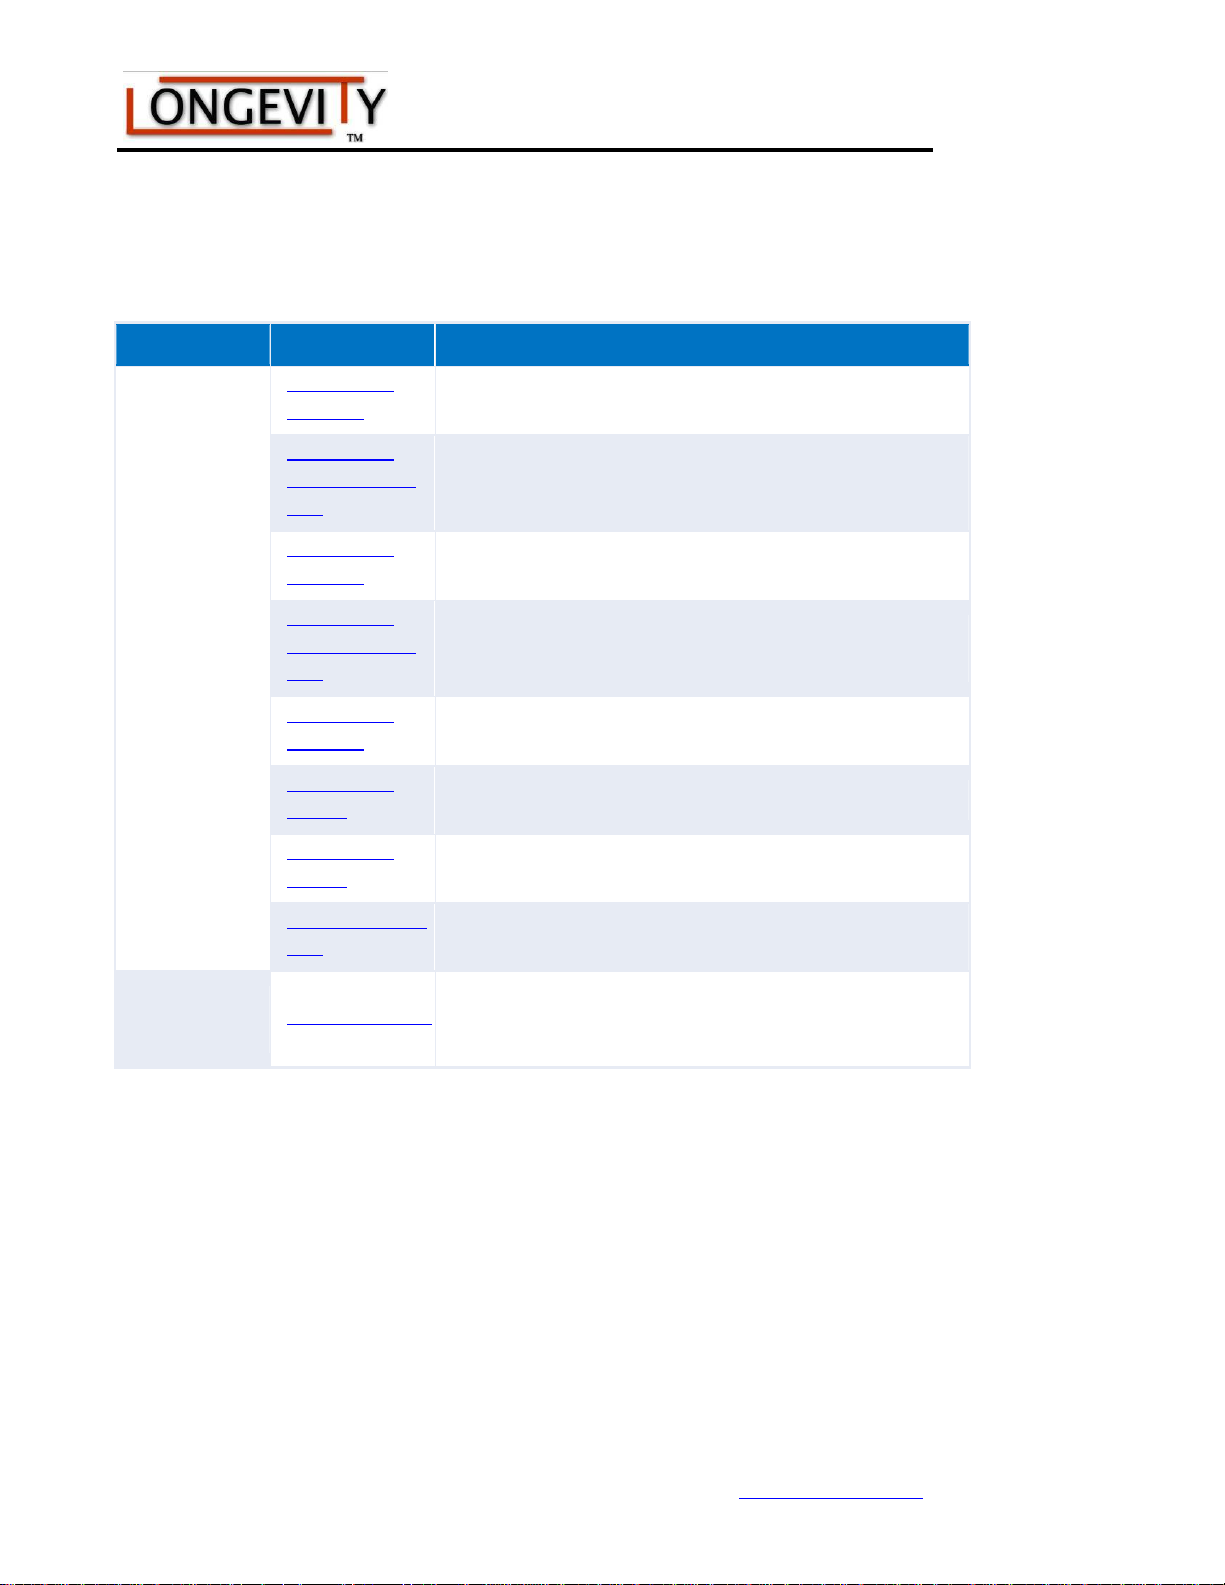
Technology
Plasma Cutters
Typical Applications
MOSFET
Technology
ForceCut®
LP-40D
Hobbyist, Auto-Body, Plumbers, Sheet Metal Work,
Thin Material, HVAC
ForceCut®
LP-40D Pilot
Arc
Hobbyist, Auto-Body, Plumbers, Sheet Metal work,
Thin materials. Pilot Arc enables easier Arc Starting25
lbs (28 lbs Boxed)
ForceCut®
LP-50D
Hobbyist, Light Industrial, Commercial, Fabrication,
Maintenance, Light Construction
ForceCut®
LP-50D Pilot
Arc
Hobbyist, Light Industrial, Commercial, Fabrication,
Maintenance, Light Construction
ForceCut®
LP-60D
Boat Repair, Commercial, Light Industrial, Body
Shops, Repair
ForceCut®
LP-70
Commercial, Industrial, Repair, Fabrication
ForceCut®
LP-80
Manufacturing, Repair, Heavy Fabrication,
Construction, Industrial
MaxArc® LP100
Manufacturing, Industrial, Construction, Heavy Duty
Fabrication, Automation
IGBT
Technology
ForceCut® 60I
Portable Fabrication, Industrial Repair, Heavy
Manufacturing, Thick metal cutting, Commercial Use,
Construction, Fab Work
PLASMA CUTTERS www.LWELD.com
Typical Applications Chart of Plasma Cutters:
20 www.longevity-inc.com
Page 25
Plasma Cutters www.LWELD.com
LP-
40D
Cutting Methods
Different material thicknesses require different cutting techniques.
Thin material: Start perpendicular to the work piece. It is unnecessary to
angle or start on the edge, as the arc will pass through quickly.
Medium material: Angle the torch tip to avoid damaging the tip. Once the
arc passes through the material, you may begin cutting normally.
Thick material: Drill a pilot hole through which to start your arc, or start on
the edge of the work piece.
Never cut material on a flat surface. Raise the work piece above the surface to avoid
blow back which may burn you or cause fires.
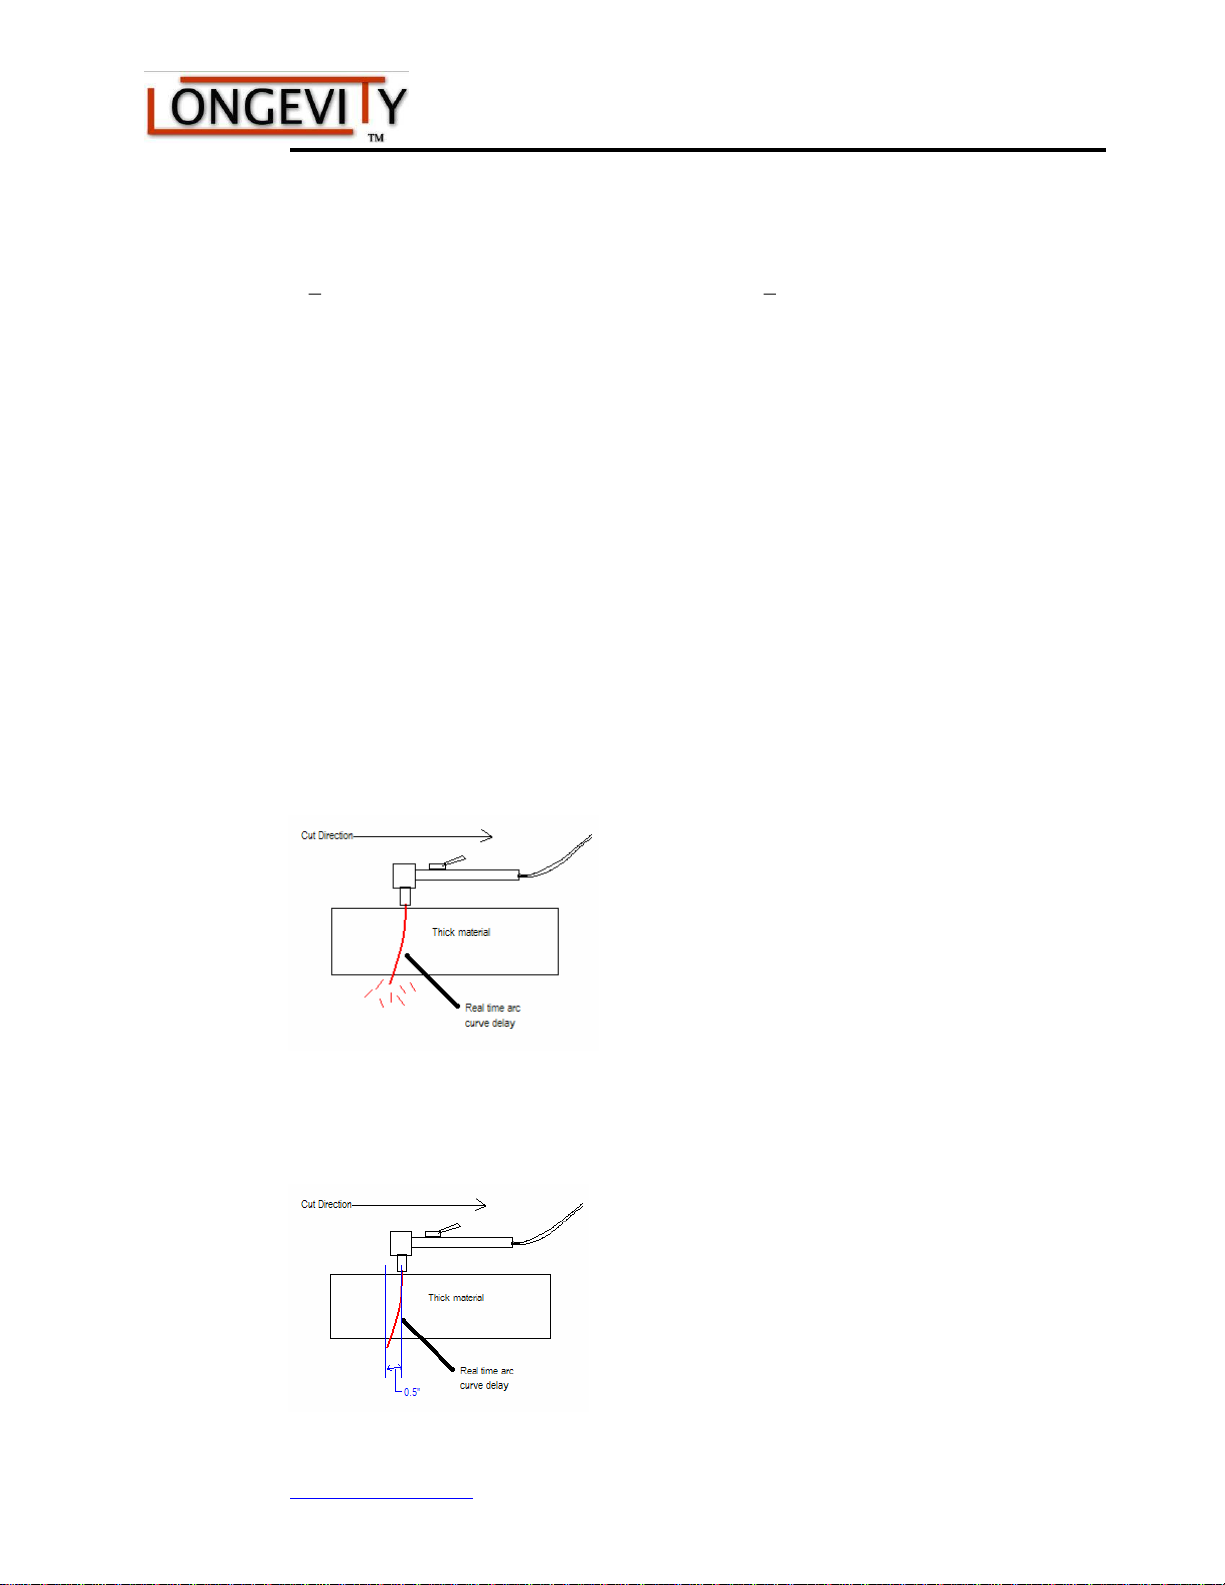
Real Time Arc-Curve Delay
When cutting thick materials you must maintain a steady even motion in the
direction of the cut. Moving the torch too quickly causes an arc-curve delay. An
arc-curve delay can leave the work piece with uncut sections, requiring you to re-cut
those sections, which could distort or damage the work piece.
To avoid arc-curve delay, allow the arc to pass completely through the work piece
before moving too far ahead. The arc-curve should lag not more than the thickness of
the material being cut. In other words, if the work piece is one-half inch thick, the arc
curve should lag not more than one-half inch behind the torch, as shown below.
www.longevity-inc.com 21
Page 26
Tips For Plasma Cutting provided by:
www.plasma-cutters.com
www.freeweldingforum.com
Using a LONGEVITY Plasma Cutter with either High Frequency or
Pilot Arc technology is very easy to use, and since each
LONGEVITY unit is quality tested at our in house testing facility
before it is shipped , most of our customers take right out of the box,
plug it in and get to work. Naturally, it is easy to understand how
excited you would be to see the delivery truck pull up with your
brand new LONGEVITY Plasma Cutter and you should be.
Congratulations is in order and we want to ensure you have the best
experience with your LONGEVITY Plasma Cutter. However,
excited as we are you can't wait to put your LONGEVITY Plasma
Cutter into action, we would like you to consider these helpful tips
and examples that will enable you to get the most out of your
LONGEVITY Plasma Cutter and it's consumables. So, before using
your LONGEVITY Plasma Cutter it is extremely important to read
the owner's manual all the way through regardless of your experience
level. Even if you are a seasoned veteran, give it a once through and
keep it near by in case you, someone you know or someone you
work with has a question about the use or specifications of your
LONGEVITY Plasma Cutter.
At this point, let us assume that you have purchased the
LONGEVITY Plasma Cutter that is right for you, and even though
you did your research already, it is always a good idea to revisit the
safety precautions, specifications and unique options ensuring you
achieve the most with your LONGEVITY Plasma Cutter while
staying safe. In case you have not decided which LONGEVITY
Plasma Cutter is right for you, please visit the Help Me Choose
section and take advantage of the LONGEVITY Smart Selector.
In terms of safety, the price of carelessly cutting corners can be
extremely costly, not only to your health but to the people around
you as well. So, before you get started using your LONGEVITY
Plasma Cutter to create your master piece, build a bridge, or
whatever you want to do, make sure you have a quality safety
checklist you follow after you read the manual and before you get
started. Below are a list of tips and safety measures you might find
useful in developing your safety checklist. Remember, in no way
shape or form does this checklist or any other check list ever replace
the necessity of thoroughly reading the owner's manual of your
LONGEVITY Plasma Cutter.
PLASMA CUTTERS www.LWELD.com
22 www.longevity-inc.com
Page 27
Plasma Cutters www.LWELD.com
Check List Suggestions
Connect the air supply to your LONGEVITY Plasma
Cutter and consult your owner's manual to ensure the
correct PSI. The PSI is about 65-75.
Each LONGEVITY Plasma Cutter, regardless if it
uses Pilot Arc or High Frequency technology, comes
with an air flow regulator and water catcher.
Reference the owner's manual of your LONGEVITY
Plasma Cutter for specifications and care instructions
of your air flow regulator and filter.
Check the torch of your LONGEVITY Plasma
Cutter and make sure everything is in order.
Reference the owner's manual of your LONGEVITY
Plasma Cutter to make sure all of your consumables
are clean, correct, and pieced together securely
before you begin cutting.
Gouging or piercing can be achieved by simply
lowering the amperage output and keeping with the
recommended psi. Examples on how to achieve the
desired results can be referenced in the owner's
manual of your LONGEVITY Plasma Cutter.
Now you are ready to use your LONGEVITY
Plasma Cutter safely and efficiently. Turn the
machine on and enjoy the satisfying experience of a
quality LONGEVITY Plasma Cutter.
Double check your air supply, air flow regulator and
water filter. (More on this below.)
All LONGEVITY Plasma Cutters require a solid
ground connection as close to the work piece as
practical. Remember, even though your
LONGEVITY Plasma Cutter can cut through paint
and other coatings on the metal, the ground
connection requires a clean, flush connection to the
work piece.
Utilizing the proper safety equipment is just as
important as understanding how to properly operate
your LONGEVITY Plasma Cutter. Consult the
owner's manual of your LONGEVITY Plasma Cutter
www.longevity-inc.com 23
Page 28
to be sure you are using the correct gloves, eye
protection, welding leathers, face shield, etc. You
can find all of the necessary equipment as stated in
the owner's manual of your LONGEVITY Plasma
Cutter in the accessories section of our website.
The old adage says to measure twice and cut once,
but we want to go ahead and suggest you make a
sample cut (of the same caliber as the intended use)
with your LONGEVITY Plasma Cutter before you
get started. Use this rehearsal just to be sure you
have correctly calibrated all the settings to work as
desired. If you are going to be cutting for a large
piece of metal, it can sometimes be difficult for even
the most experienced metal worker to cleanly stop
and start. We recommend you use the sample cut to
thoroughly rehearse the intended cut with your
LONGEVITY Plasma Cutter.
LONGEVITY Plasma Cutter Tips
In order to successfully execute a clean cut with your LONGEVITY
Plasma Cutter you must consider a combination of elements involved
in the cutting process:
The tip of your torch is designed to focus the plasma stream to the
work piece in accordance with the appropriate setting (see owner's
manual). Trying to use a 80-amp torch tip at a 40-amp setting will
not focus the energy of your torch accurately and thus lead to a
wider kerf. And the opposite scenario of using an 80-amp setting
with a 40-amp tip will abuse your torch tip and require it to be
replaced sooner than intended.
When cutting a thicker material with your LONGEVITY Plasma
Cutter it is important to use a torch tip designed for a higher-amp
output. Higher-amp tips have a larger opening than lower-amp tips.
Attempting to use a 40-amp tip to cut thick metal with a higheramp output will distort your 40-amp tip meaning it will need to be
replaced.
Each LONGEVITY Plasma Cutter, both Pilot Arc and High
Frequency , allow you to cut different metals at different
speeds. For example to achieve a quality cut of 1/2in. thick
steel with the LONGEVITY Force Cut LP-40D Pilot Arc
your speed will be roughly 7 inches per minute. Where as
the LONGEVITY Force Cut LP-80D will cut 1.25in. thick
steel at the same rate.
PLASMA CUTTERS www.LWELD.com
24 www.longevity-inc.com
Page 29
Plasma Cutters www.LWELD.com
Use extended tips on your LONGEVITY Plasma Cutter for tough
to reach corners, tracing a pattern, or areas with tight spaces.
Pilot Arc technology allows you to ignite the arc without the tip
touching the metal. Use a torch guide or tip shield to protect your
consumable. The more often you drag your torch tip across the
material or stop and restart the Pilot Arc, the shorter the life span of
your consumables will be.
Using a torch guide or tip shield is a great way to protect the
consumables of your LONGEVITY Plasma Cutter. Remember to
maintain a 1/16in. - 1/8in. distance from the material when cutting.
* The important things to consider while using your LONGEVITY
Plasma Cutter to cleanly execute a cut is correct amperage of the torch
tip, thickness of the material, intended speed, proper technique, and
ultimately protecting the life of your consumables.
Cutting Posture
Sometimes you may find that you are unable to use a guide or shield
when operating your LONGEVITY Plasma Cutter. In some instances a
project may be a very ornate design with different curves and
protrusions or the material is too thick to apply a shield or guard to
your LONGEVITY Plasma Cutter torch tip. In order to maintain the
quality and consistency of your work we recommend that you use your
other hand as a guide. Give yourself a fighting chance to steady your
hands and take advantage of the protective gear you have like our guys
on the LONGEVITY Facility Testing Team .
One of the reasons you purchase a LONGEVITY Plasma Cutter
is because of it's quality. Therefore, we think you should have a
few quality reminders to think about when you are cutting.
If you stop and start an arc in the middle of a cut, often the the quality
of your cut will suffer and compromise the integrity of your so far
clean cut-line. Remember, even when we do facility testing, a suitable
method to apply when using your LONGEVITY Plasma Cutter is
rehearsing the cut. Be sure you are going to be able to produce a
smooth continuous cut-line all the way through.
Along with rehearsing your cut, another equally good reminder is to
protect your consumables as much as possible. Often we can get
comfortable piercing right through thin steel with our LONGEVITY
Plasma Cutters, but when cutting thicker metal often the intense back
splash from initial contact will rapidly wear down your torch tip and
other consumables. Even though the seeing the bright sparks show off
www.longevity-inc.com 25
Page 30
the awesome power of your LONGEVITY Plasma Cutter, remember
we want you to be able to enjoy the results of your work time and time
again. So, in situations when you are going to be cutting thick metals at
high amperage with your LONGEVITY Plasma Cutter, we recommend
you start with the torch pointed at a 45 degree angle. This angled
approach allows for the first blast of metal to be released with out back
splash on to your valuable consumables.
Know Your Amperage, Know Your Metal
At www.longevity-inc.com, you can see the cutting thickness
capability.
Understanding the amperage in relation to your cut speed is important.
Some metals respond differently than others. For example the faster
you move on a material such as aluminum, the cleaner your cut will be.
Conversely, when using your LONGEVITY Plasma Cutter to cut
thicker material, set your unit to full output and vary your travel speed
accordingly. Thin material requires you to turn down the amperage and
change to a lower-amperage to achieve a narrow kerf.
Figuring out if you are going too slow or too fast can be a daunting task
that really only comes with time and experience. However, our guys in
the LONGEVITY Facility Testing Team have a few pointers for you:
If your cut has a lot of spray back then you are probably going
too fast.
If the arc exits the material going straight down then you are
probably moving too slow and you will have an unnecessary
buildup of "dross" or "slag."
Your arc should be exiting the material at a 15 - 20 degree angle,
but opposite the direction of your cut path.
Using A Cutting Guide
First thing in using a torch guide with your LONGEVITY Plasma
Cutter is make sure it isn't flammable! Aluminum works as a great
torch guide, but be sure it is attached to the torch cup and not the torch
tip. Aluminum is a great contact guide because of it's smooth surface
but be wary of the torch tip because of electrical conductivity of
aluminum. It would be a terrible mess of a cut, loss of consumables,
and overall depressing mistake if your torch guide melted to the torch
tip or the project at hand. Next you want to mark the material to be cut
with either white chalk or a black marker. If you are unsure of how
steady your hands are, we recommend you try using a straight edge
clamp attached to the work piece or torch guide.
PLASMA CUTTERS www.LWELD.com
26 www.longevity-inc.com
Page 31
Plasma Cutters www.LWELD.com
All articles are composed by the LONGEVITY Facility Testing Team
and are written with expressed interest of maintain a strong standard in
LONGEVITY Global Inc. quality, to help address topics, and answer
questions for amateur and experienced users alike. Please remember to
always exercise extreme causation and abide by all provided safety
specification.
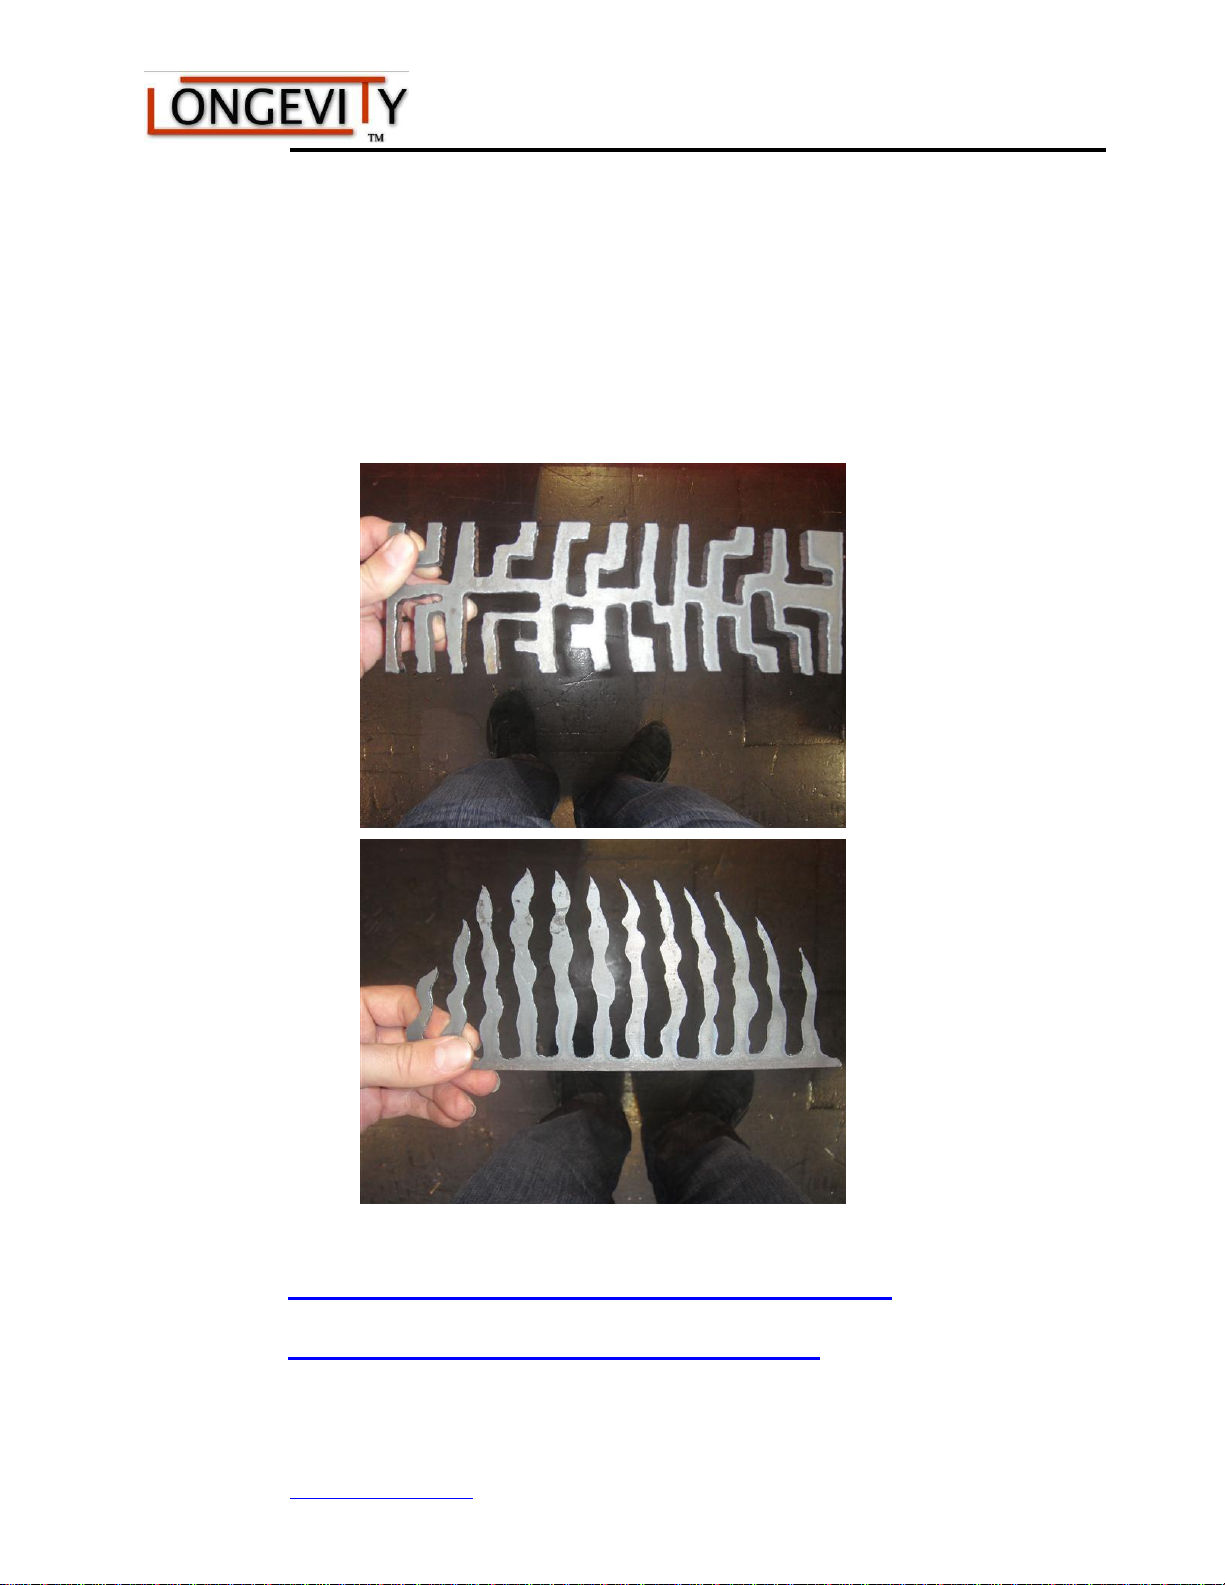
Sample Photos:
For more information on plasma cutting from professionals go to
www.freeweldingforum.com and
www.plasma-cutters.com
www.longevity-inc.com 27
Page 32
PLASMA CUTTERS www.LWELD.com
Routine Maintenance
The life of your machine and the quality of the work performed using your machine,
will be enhanced by practicing periodic routine maintenance.
At regular intervals, clear dust that may accumulate in the machine using
clean and dry compressed air. If the working condition has heavy smoke and
pollution, the welding machine should be cleaned once a month.
Keep the machine exterior clean with mild soap and water.
Do not walk on or store items on the cables or cords.
Do not jar, drop, or stack items on top of the machine.
Always connect the machine to a well grounded electrical outlet.
Always check the torch consumables before and after use and ensure that
they are clear of obstructions, and that no parts are damaged.
Replace any worn or damaged consumables before using machine.
For periods of prolonged non-use, remove cables and store them in their
original boxes in a cool dry place.
28 www.longevity-inc.com
Page 33
Plasma Cutters www.LWELD.com
Problems, Causes, and Solutions
Problems
Causes/
Solutions
Machine will not
turn on.
LONGEVITY
The machine runs,
but nothing is
happening
pressure. Make sure the regulator adjustment knob is turned
clockwise and allow pressure. Check the consumables and make
sure they are properly assembled. Check the ground clamp and
proper grounding to the unit. Check pilot arc wire to insure it is
properly connected to the unit.
Consumables
(tips) are being
consumed
leaks in the hose, maintain a distance of 1/8” from the torch tip or
workpiece. If your unit comes with a manual Post Flow 2.5 or 5.0
switch make sure you leave it on 5.0 for more air to pass cooling
your torch tips.
Heavy Underside
Slag (Cutting)
Poor Cut Quality
desired thickness of material. Check the consumables to insure they
are producing a stable arc. Replace Consumables and insure you
have the proper PSI at the regulator.
Inconsistent
Arc
replace consumables and adjust the regulator to proper PSI
O.C. Over
Current LED
Lights
machine on and allow fans to cool the machine. You can also turn
the machine off to properly cool it. Do not continue to weld until
light is off.
Issue Not Listed
Troubleshooting
If your unit is not properly functioning, please call us immediately toll free at 1-877566-4462 for support. We have included a small table here to diagnose most
common problems.
www.longevity-inc.com 29
Page 34
PLASMA CUTTERS www.LWELD.com
LONGEVITY® Global, Inc. thanks you for your purchase and opportunity to be able
to serve you. If, after reviewing this manual, you have any problems in setting up or
operating your machine, contact us at [email protected].
LONGEVITY® Global, Inc.
Toll-Free 1-877-LONG-INC / 1-877-566-4462
Website: www.longevity-inc.com
Sales: [email protected]
Customer Service: [email protected]
Dealers: [email protected]
Please join our welding forums to share welding tips and tricks, to receive useful
information from customers who also use our products, and to be a part of the
LONGEVITY® welding community at www.freeweldingforum.com
For the coolest LONGEVITY sponsored race teams plus a complete racing forum
that covers everything from Drag Racing to RC Car Racing, please check out
www.longevity-racing.com!
Enjoy your new plasma cutter from LONGEVITY! Thanks again!
30 www.longevity-inc.com
 Loading...