

Page 1
Leigh Router Joinery Jigs
Dedicated Customer Support
1-800-663-8932
Joining Tradition with Today
Page 2
ii
Your New Leigh Dovetail Jig
SUPERJIG-12-18-24 User Guide
Congratulations! You now own a most useful and versatile
dovetailing tool. The Leigh Superjig Dovetail Jig will help you
cut an infinite variety of joints, and all of its major functions
are described in detail in this user guide, plus there’s a slide-out
Quick Reference Guide underneath the jig. A very helpful
DVD is also included, but the user guide is essential reading.
We recommend that you first assemble and mount the jig,
carefully following the instructions in the first section of the
user guide. Then read the rest of the guide, following along
with the basic functions and principles of operation, before
you try to do any actual joinery routing. By all means, cut a
few practice joints in scrap boards before you use the jig to
rout a precious hardwood work piece!
If you have questions not answered in this user guide, please
call the Leigh customer support line: 1-800-663-8932
or email Leigh: [email protected].
But remember: “If at first you don’t succeed, read the instructions!”
CONTENTS and STANDARDS
*See Appendix IV – Customer Support
Important! Inches and Millimeters
The Superjig can be ordered in inch or metric versions. They’re
identical except for the calibration scales. This Leigh Englishlanguage user guide show measurements in both inches and
millimeters, with “inches” first, followed by “millimeters” in
square brackets.
3
Example:
⁄4"x 51⁄2"x 8" [20x 140x 200mm]
Do not be concerned if the inch/millimeter equivalents are not
exact. Just use the dimensions which apply to your jig.
1
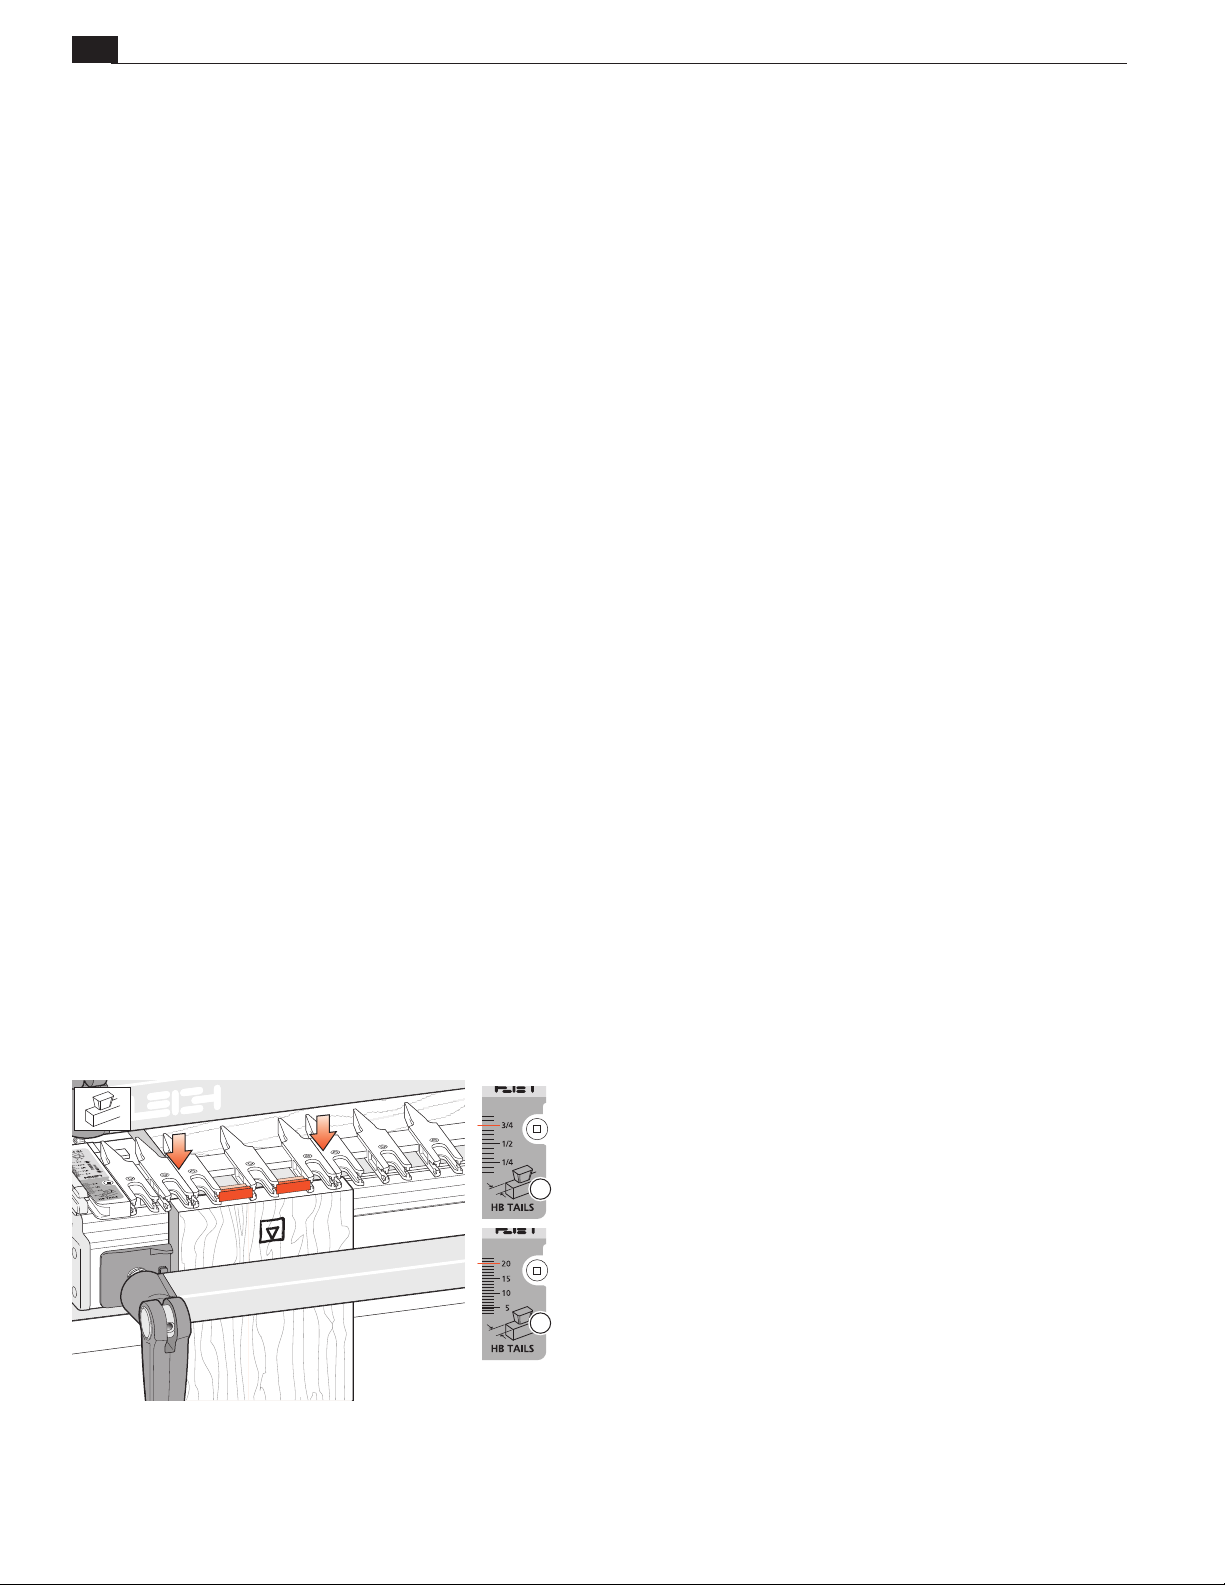
Where finger assembly scales overlay an illustration, the “inches”
scale
will be at the top, the “millimeters” scale will be at the
bottom. Only the front “active” half of the scales are illustrated.
For clarity, setting positions are indicated with a red line in the
user guide only. On the jig, the lines are black.
2
Page 3
CONTENTS and STANDARDS
SUPERJIG-12-18-24 User Guide
Contents and Standards ........................................................................................... iii
Chapter 1 – Jig Assembly, Mounting, and Using The Clamps .................................. 1
Chapter 2 – Adjusting the Finger Assembly ............................................................. 7
Chapter 3 – The Leigh e-Bush and Optional Guidebushes ....................................... 9
Chapter 4 – Basic Jig Functions and Scale Modes ................................................... 11
Chapter 5 – Using Your Jig Safely ............................................................................ 13
Chapter 6 – Wood Preparation ................................................................................ 15
Chapter 7 – Router Preparation ............................................................................... 17
Chapter 8 – Through Dovetail Procedures .............................................................. 19
Chapter 9 – Variably Spaced Half-Blind Dovetail Procedures ................................ 29
Chapter 10 – Single Pass Half-Blind Dovetails ........................................................ 37
Chapter 11 – Rabbeted Half-Blind Dovetails .......................................................... 45
Chapter 12 – Asymmetric Dovetails ....................................................................... 47
Chapter 13 – Sliding Dovetails ................................................................................. 51
Chapter 14 – Box Joints ............................................................................................ 57
Chapter 15 – Hints and Tips ..................................................................................... 63
Appendix I – Attaching the Leigh e-Bush to the Router ........................................ 67
Appendix II – Bit Selection ....................................................................................... 69
Appendix III – Jig Parts ............................................................................................. 75
Appendix IV – Customer Support ............................................................................ 79
iii
Page 4
iv
1
3
SUPERJIG-12-18-24 User Guide
Glossary of Symbols
CONTENTS and STANDARDS
To help you understand the instructions and illustrations in this
user guide, we have used a number of international symbols, plus
a few special ones of our own. They are all explained below. You
needn’t worry about memorizing these symbols now, because
they are repeated quite frequently throughout the user guide,
and you will soon get used to them.
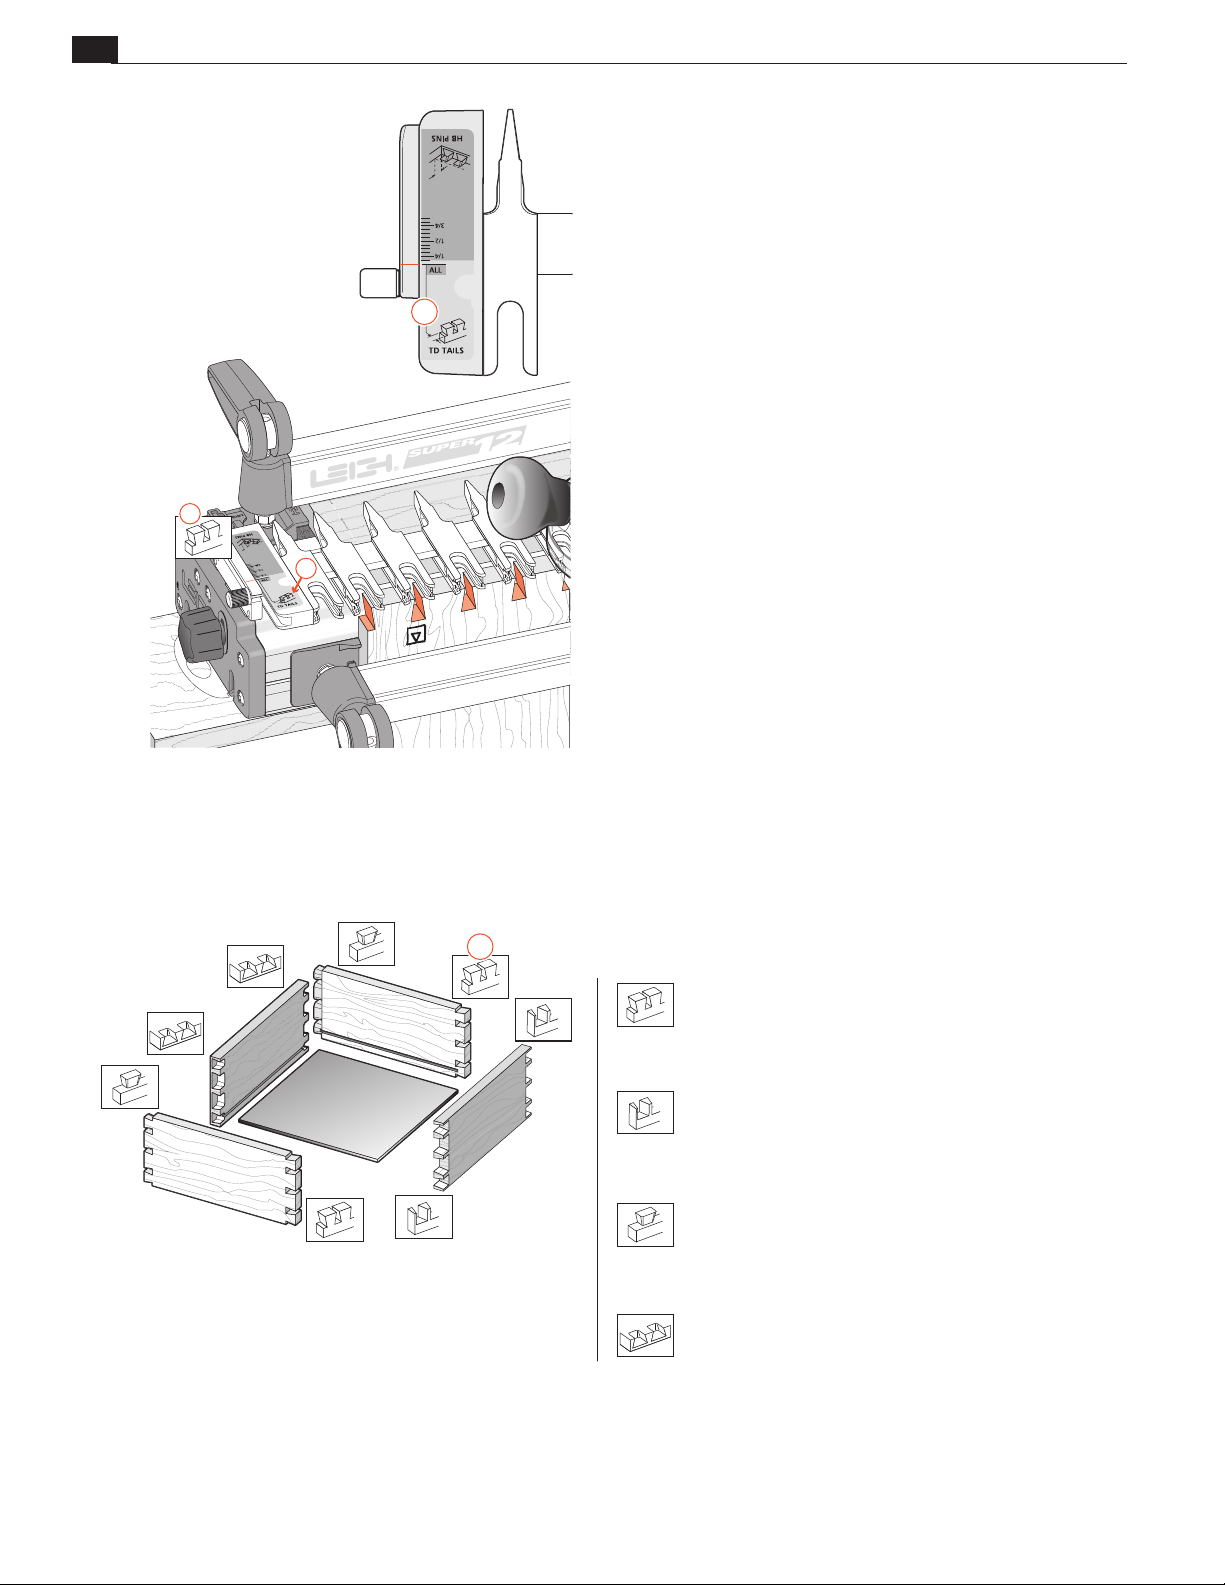
The Leigh jig’s guidefinger assembly can be in any one of four
joint modes, depending on what type of joint and which part
of the joint you are routing. Each finger assembly scale has it’s
2
own mode icon
, identifying that joint part. You will also find
the joint mode icon in the top left corner of most illustrations
1
, indicating which finger assembly mode to use.
Sometimes a joint mode icon will be used to identify a board .
These are the four joint mode icons:
TD Tails
(tails for through dovetail joints)
TD Pins
(pins for through dovetail joints)
HB Tails
(tails for half-blind dovetail joints)
HB Pins
(pins for half-blind dovetail joints)
Page 5
CONTENTS and STANDARDS
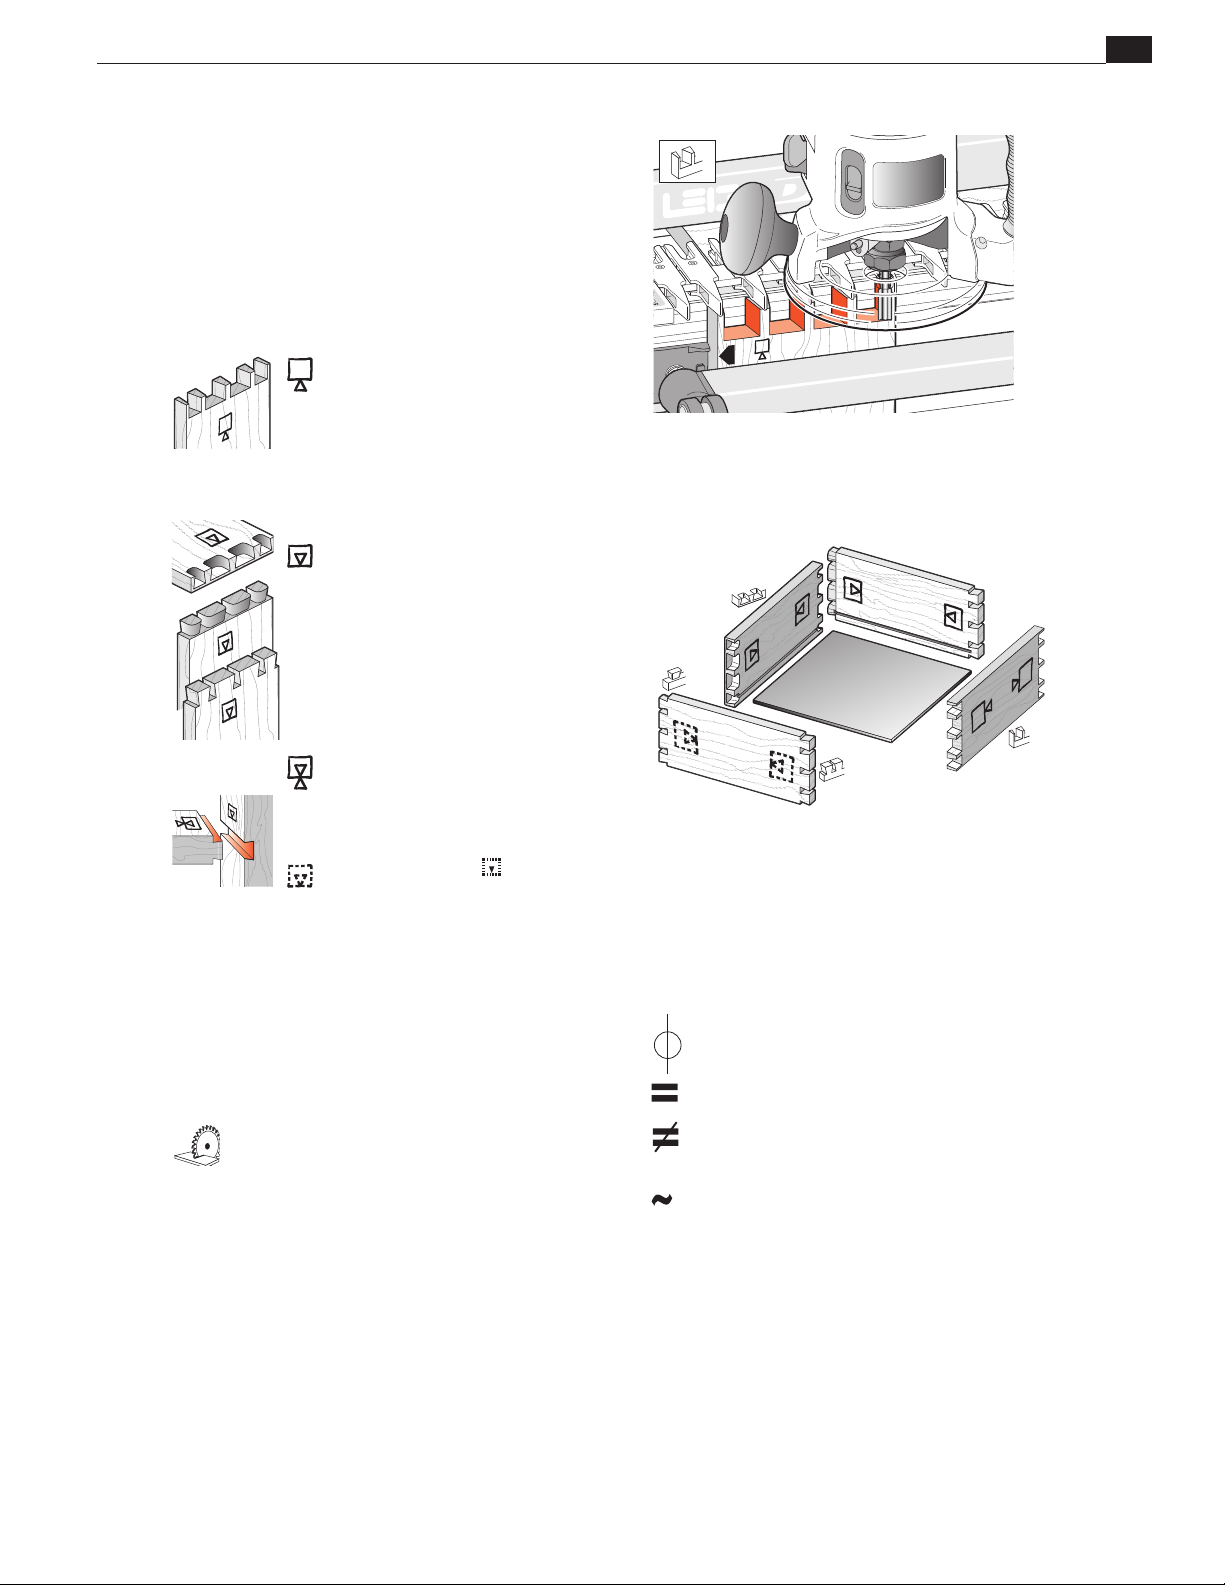
Which Way Round Should the Board Go?
As virtually all dovetail joinery is used to make boxes,
drawers and chests etc., we devised these simple (and
hopefully intuitive) icons to indicate which side of a
board faces inwards or outwards on the finished “box”,
and which side of the board faces outward (toward
you, the operator), when it is clamped in the jig.
SUPERJIG-12-18-24 User Guide
This icon o indicates the “outside”
of a board. All through dovetail
pin boards are mounted in the
jig with this “outside” face away
from the jig (toward you, the
operator).
This icon i indicates the “inside”
of a board. All half-blind pin and
half-blind tail boards, and through
dovetail tail boards, are mounted
in the jig with the “inside” face
away from the jig toward you,
the operator.
v
This icon j indicates boards that
are mounted both ways e.g. sliding
dovetails and box joints.
Dotted line icons indicate the
“other” side of the board in the
illustrations.
The following symbols indicate:
This edge against sidestop
e
This edge against sidestop
f
Sawcut allowance
Caution: use special care for this
operation
Numbered References in text
Centerline of board or layout
Equals
Does not equal
Approximately
Page 6
vi
Leigh VRS
Vacuum & Router Support
SUPERJIG-12-18-24 User Guide
CONTENTS and STANDARDS
Dust-Free Routing!
The revolutionary Leigh VRS Vacuum & Router Support* provides almost 100%
dust and chip collection as well as amazing full width router support. The VRS
is a must-have for all Leigh dovetail jig owners.
*US patent: USPN 7,507,060 B2 UK patent: GB2446909
Here’s How It Works
The VRS is mounted on brackets on the front of the jig and the router is supported by the finger assembly and the full width beam of the VRS. The vacuum
chute rides under the router support beam. Control arms, attached to the
vacuum chute, surround the router. These arms are adjustable to accommodate
any router base. As the router moves across the joint, the vacuum chute glides
effortlessly from side to side on nylon rollers. The chute is always in perfect
position to catch the dust and chips thrown out by the router bit. Chips and
sawdust are drawn into the vacuum chute and down through the vacuum hose.
Each VRS comes complete with two adaptors to fit all popular vacuum hose
sizes and the VRS can be used with a small shop vac or a large built in system.
The VRS is easily attached without jig modification. Each VRS comes complete
with all mounting hardware needed for any Leigh 24" D-Series jig, all Super
Jigs or the earlier model Leigh D1600.
The VRS is a full width router support.
When the work piece has been routed
on one side of the jig, the router can be
effortlessly moved to the other side of
the jig and parked while the work piece
is being changed. There is no need to
remove the router from the jig.
Because the vacuum box is always
in perfect position relative to the
router bit, the dust and chips coming off of the router bit are automatically drawn into the chute and
vacuum hose.
VRS Vacuum & Router Support Features
• Full width router support
• Easy on Easy Off. Powerful rare earth
magnets secure router support beam
• Park the router when not in use
• Vacuum box glides effortlessly under
router support beam
• Control arms position vacuum box
VRS Models
Item VRS12 Vacuum & Router Support for the Super 12 Dovetail Jig
Item VRS18 Vacuum & Router Support for the Super 18 Dovetail Jig
Item VRS24 Vacuum & Router Support for the Super 24 Dovetail Jig
The dust chute rides beneath the
router support beam. Control arms
ensure accurate positioning of the
chute and the size and shape of the
chute ensures total waste collection
regardless of bit size or joint type
being routed.
• Control arms adjust to any router
• No hoses to obstruct view
• No jig modifications necessary
• Models for all Leigh jigs
• All mounting hardware included
• Adapt to any hose size
Accessory Kits
Item AC12 VRS12 and 1607-8 Bit Set for the Super 12 Dovetail Jig
Item AC18 VRS18 and 1607-8 Bit Set for the Super 18 Dovetail Jig
Item AC24 VRS24 and 1607-8 Bit Set for the Super 24 Dovetail Jig
The VRS will work with almost any
shop vac or large vac system. Two
adaptors are included with every
VRS to handle hose sizes from 1"
to 2-1/2".
Standard Equipment
• Router Support Beam
• Vacuum chute
• Hose adaptors – small and large
• Support rails
• Screws and washers
• Hex key
Page 7
SUPERJIG - CHAPTER 1
Jig Assembly, Mounting,
and Using the Clamps
Make Sure You Have All the Parts.
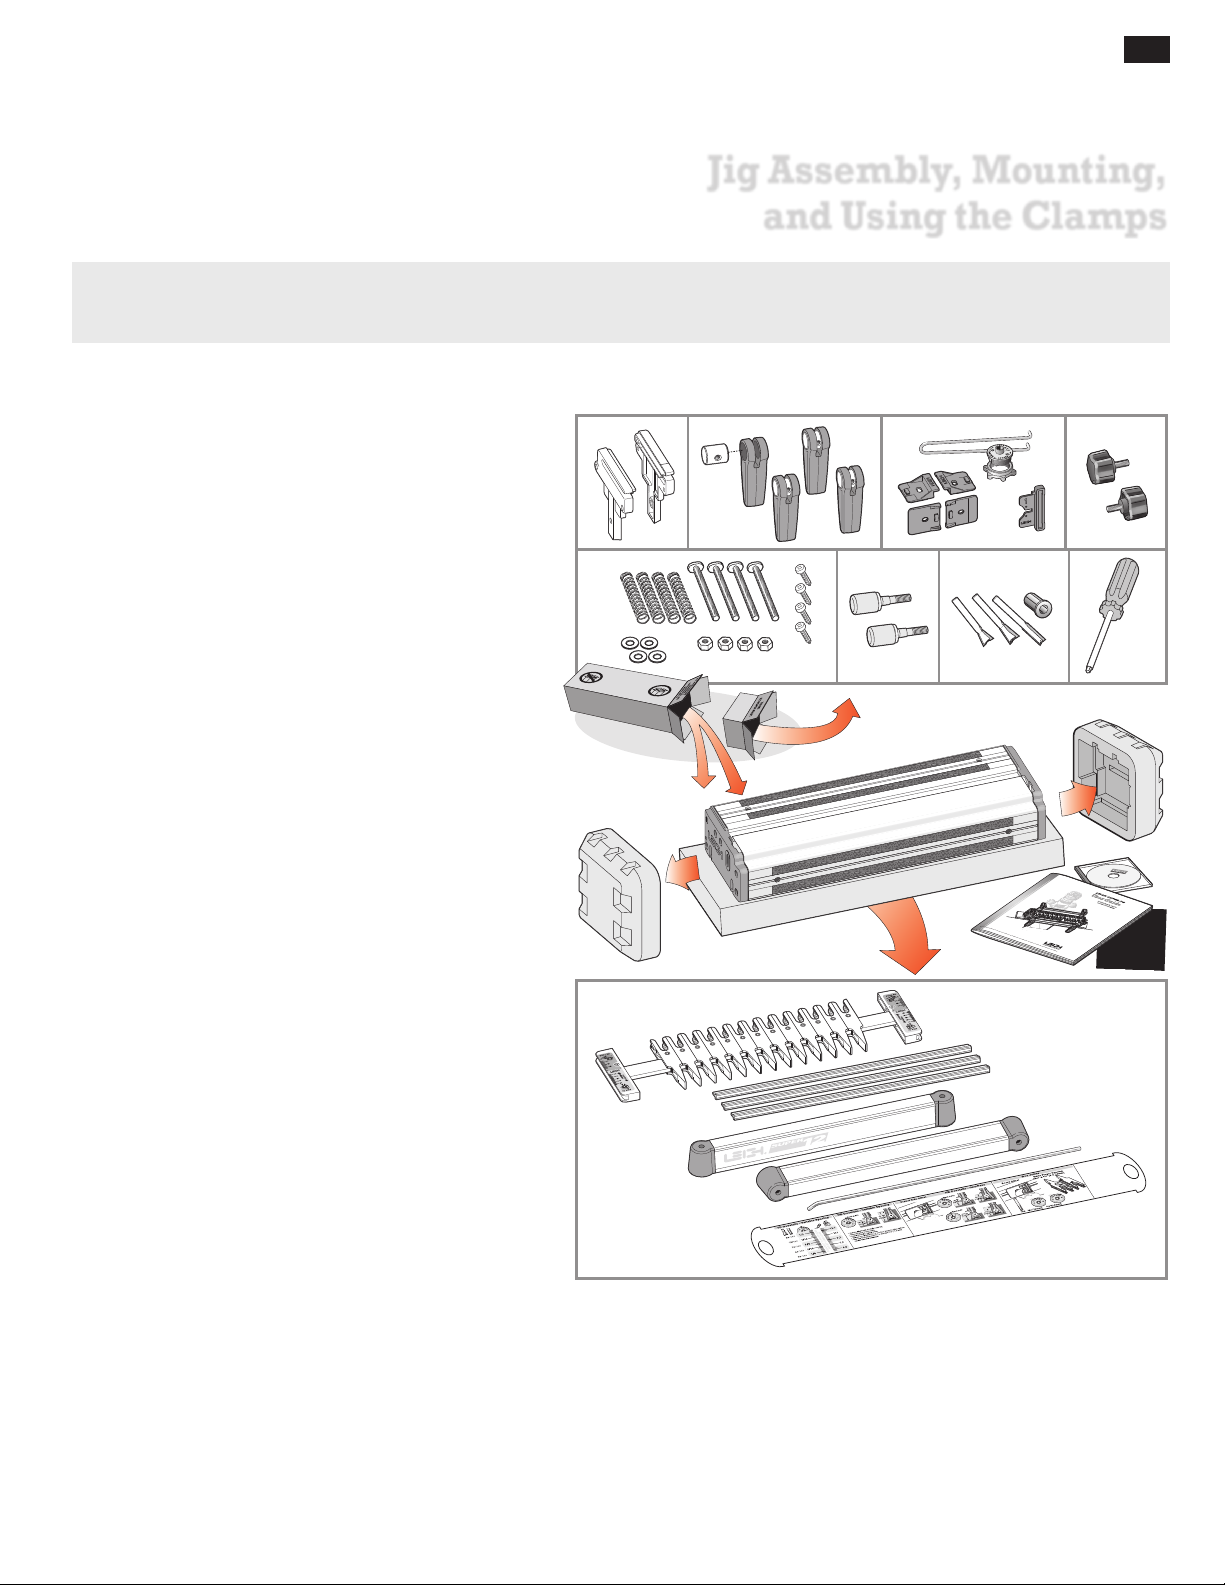
Before you start to assemble your Leigh SUPERJIG, check to make sure you have received all the required parts.
1
The small carton you removed from the end of the main
carton contains:
2 support brackets
1.
2. 4 cam-action speed clamps
4 cam clamp pivot nuts
3. 1 e7-Bush & Nut with Pin Wrench
2 each, front and rear Side Stops
1 Spacer
4. 2 support knobs
5. 4 clamp springs
4 clamp T-bolts
4 flat washers
4 T-bolt nuts
4 Jig Hold-down Wood Screws No.10 x 1"
6. 2 scale thumbscrews c/w nylon washers
7. 2 Dovetail bits, 1 straight bit, 1 Collet Reducer
Square-head guidefinger screwdriver
8.
Also included are any other small optional items you
may have ordered with your new jig. Check the packing
slip for this information.
The main carton contains:
1 main jig body
9.
1 Leigh jig User Guide
Warranty/Registration Card
DVD instructional video (English only)
1 2 3
65 7 8
9
10
4
The large inner box contains:
1 finger assembly on a bar, complete with scales
10.
Super12, with 13 guidefingers
Super18, with 16 guidefingers
Super24, with 19 guidefingers
2 lengths bridge material – see Chapter 9
1 crosscut fence (same as bridge) – see Chapter 13
2 clamp bars c/w end plugs
1 Nylon Stop Rod – see Chapter 10
1 Quick Reference pull-out card
If any items are missing from your jig, contact your supplier
or Leigh Industries immediately.
Important Note
Mount your jig securely, assemble it completely,
and make sure you have read and understood the
Safety section of this user guide before using the jig.
Page 8
2
3
Chapter 1 Sup er Jig -12-18-24 User Guide
5
2
4
1
4
JIG ASSEMBLY, MOUNTING, AND USING THE CLAMPS
1
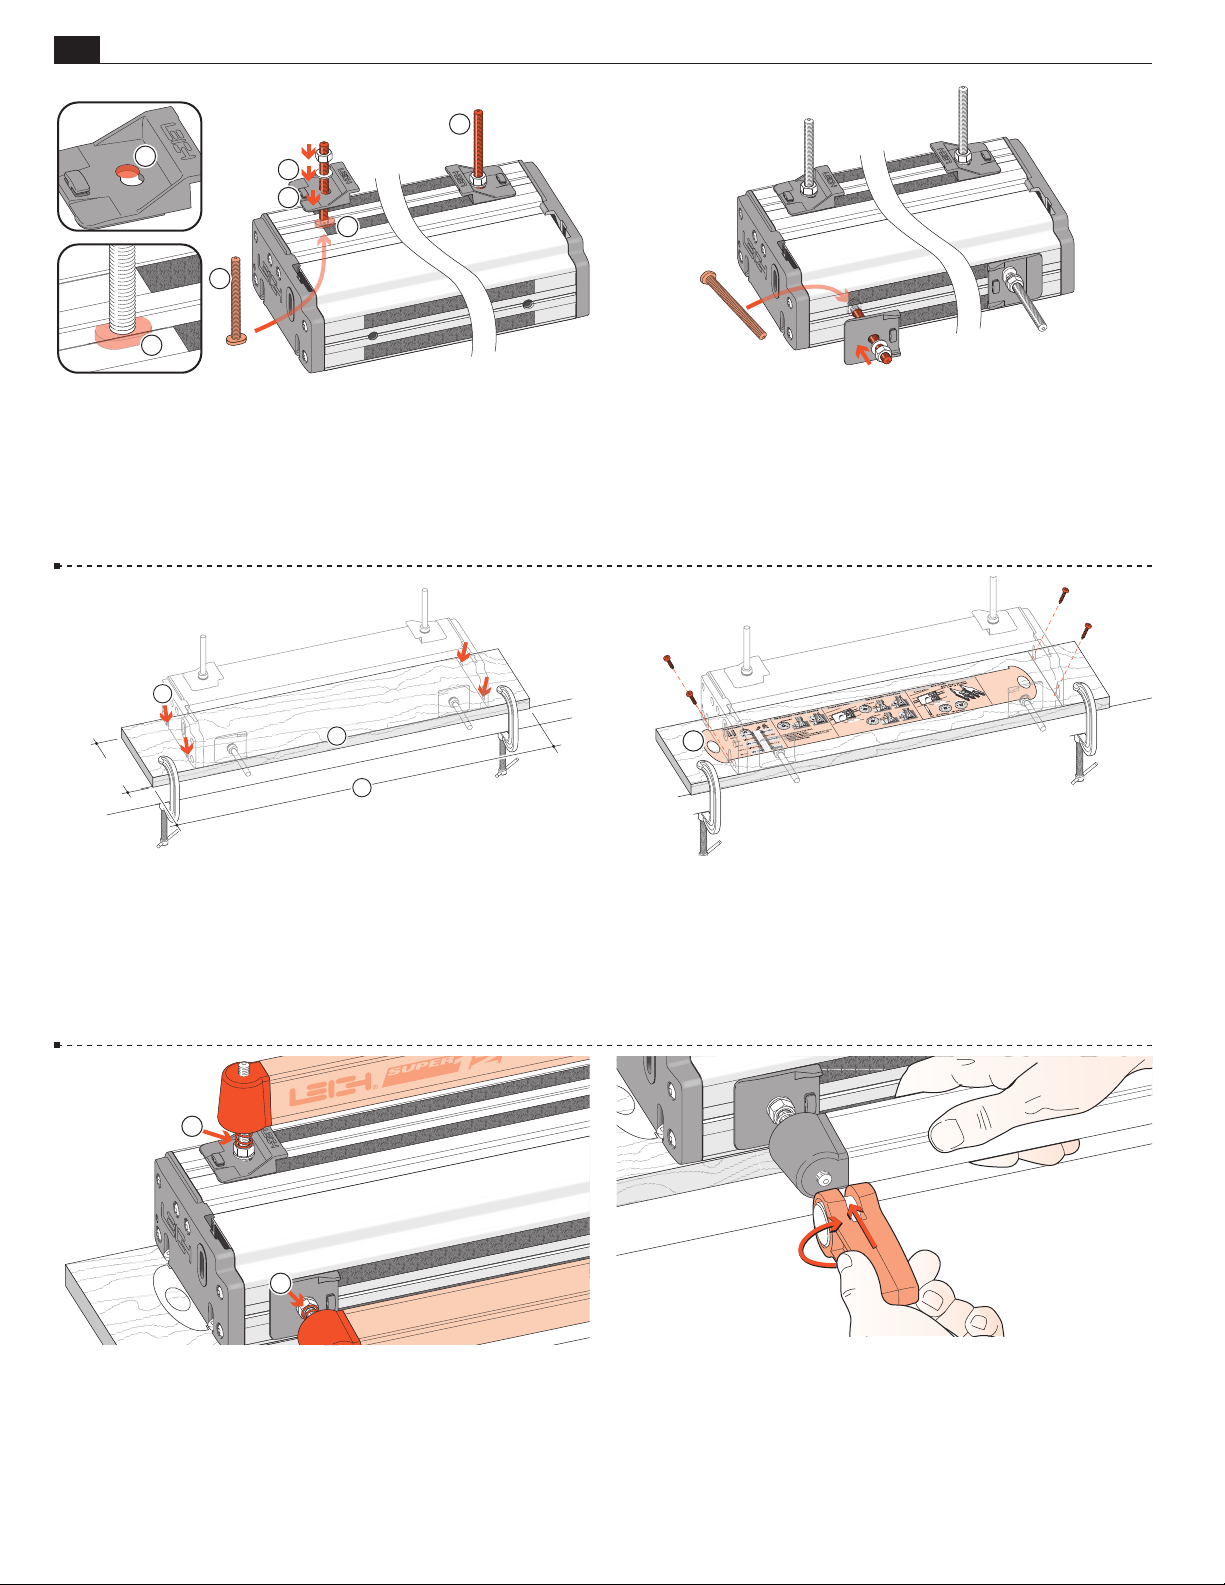
1-1 Install Side Stops Insert two clamp T-bolts through the
rear jig body holes and place a “stepped” rear side stop over each
bolt , using the rear part of the double-hole . Make sure the
bolt's “T” is between the extrusion ribs
➃. Don’t forget the steel
washer ➄ and use a ½"[13mm] wrench to tighten the nuts.
3
2
5"
[125mm]+
1
1-3 Prepare a flat ¾"[20mm] mounting board (plywood or MDF),
at least 5"[125mm] wide. Length : 26" for Super12, 32" for Super18,
40" for Super24 [660, 830 or 1000mm respectively]. Clamp it to the
front of your bench. Center the jig on the board, front face slightly
overhanging the board edge . Mark the four hold down screw positions. Drill small pilot holes at a slight angle .
1-2 Insert the two front clamp T-bolts through the jig body
holes. Make sure the bolt's “T” is between the extrusion ribs.
Place a front side stop and steel washer over each bolt but only
finger-tighten the front nuts; you will need to index these to the
rear stops later.
1
1-4 Quick Reference Pull-Out Decide which end
of the jig you wish to access the “Quick Reference” instruction
pull-out and place the jig over the pull-out . Using the screws
provided; screw the jig to the board. Make sure that the pull-out
slides freely.
1
1
1-5 Place four springs and two clamp bars on the T-bolts.
Make sure the clamp bars move freely on the T-bolts.
1-6 Screw a clamp lever assembly onto each T-bolt.
Page 9
JIG ASSEMBLY, MOUNTING, & USING THE CLAMPS
1
2
Chapter 1Sup er Jig -12-18-24 User Guide
3
90˚
90˚
90˚
90˚
3
1
2
4
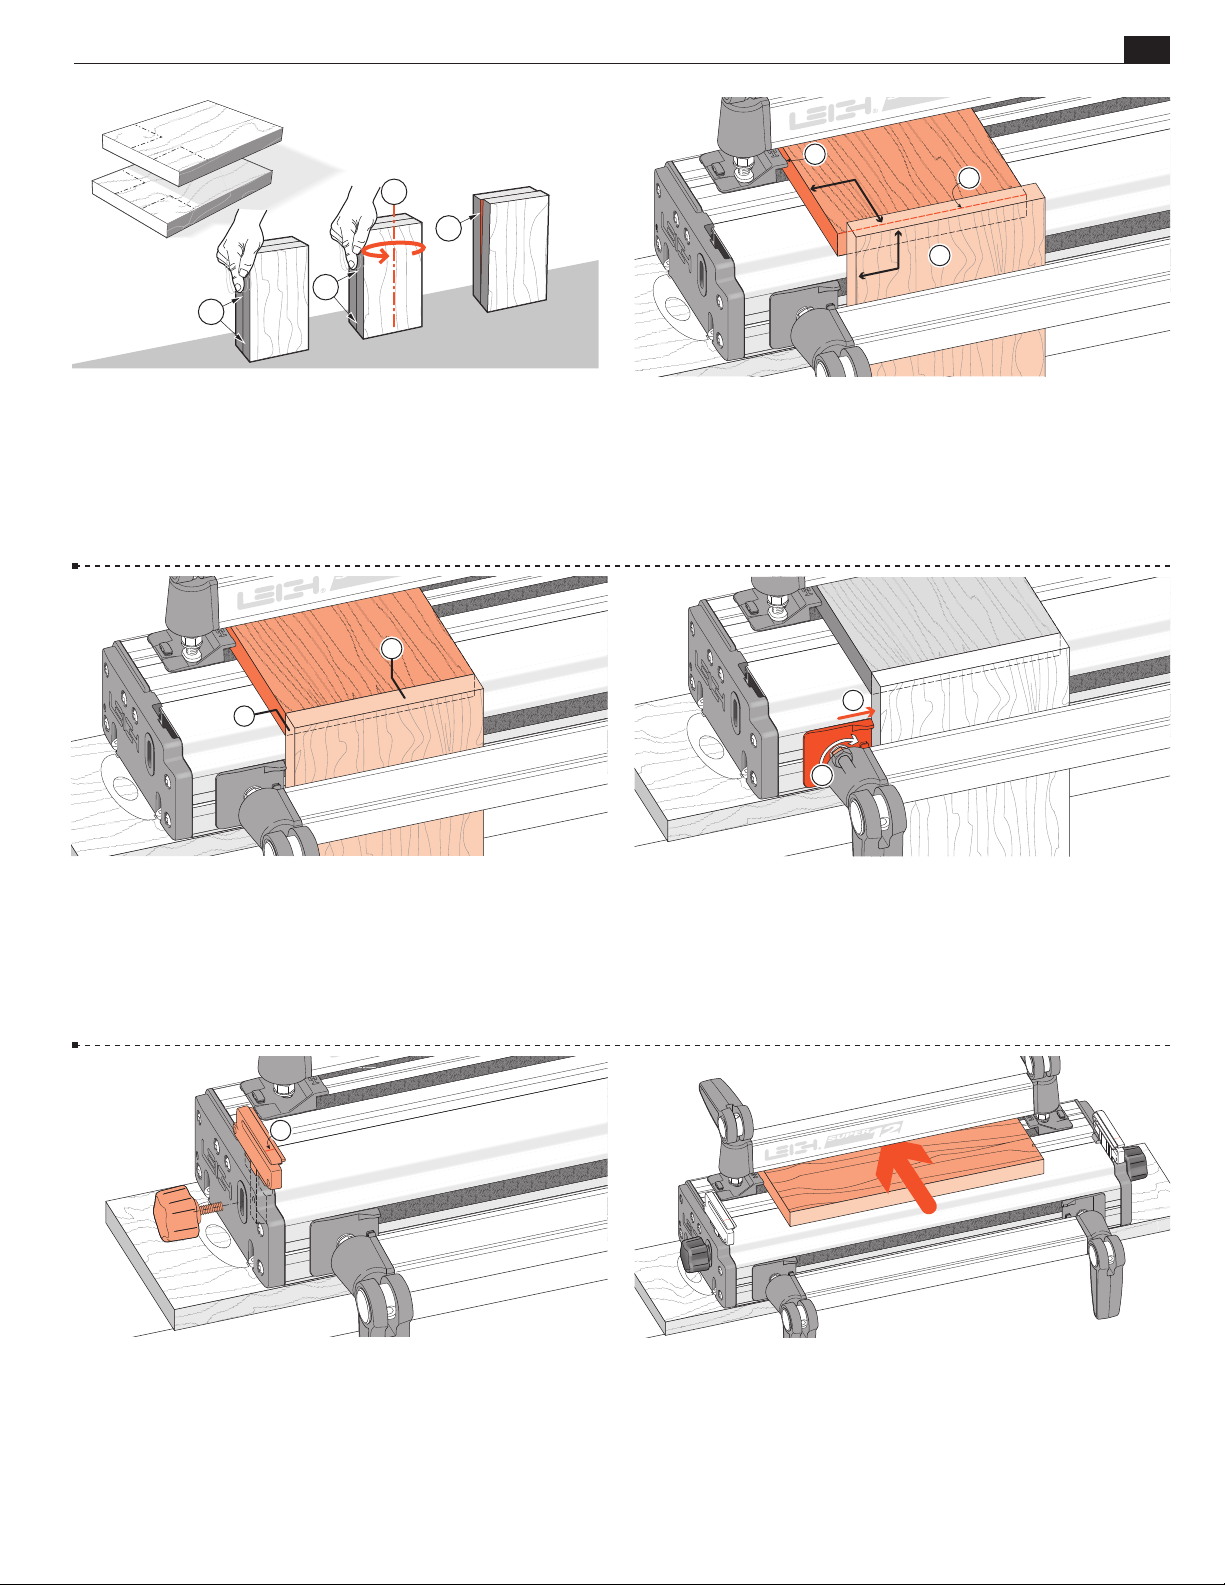
1-7 Now you need two boards about ¾" x 6" x 8" long
[20 x 150 x 200mm]. Both must have perfectly square ends to accu-
rately index the front and rear side stops.
Check for squareness: stand both pieces vertically on a flat
surface. Make sure side edges are flush at bottom and top .
Turn one piece around on its end . If side edges are flush top to bottom , the boards are square. If not, ➃; cut two that are.
1
2
2
90˚
90˚
3
1
1-8 Align Front Side Stops Clamp one square ended board
in the front, not touching the left side stop and with the top edge above
the top surface of the jig body . Place the other square board in the rear
clamp, tight against the left rear side stop , with its front edge touching
flush across the rear of the vertical board . Tighten the rear clamp.
Note: Do not overtighten the right hand clamps during this step.
1-9 Now loosen the front clamp and position the front board so
its top end edge is perfectly flush and level with the top face of the
horizontal board and, both boards left edges are also perfectly
flush . Tighten the clamp.
1
1-11 Insert the right and left support brackets. Attach the knobs,
raise them to full height and tighten the knobs.
Note: For clarity, the set lines on support brackets are shown in
red in this user guide. The actual bracket lines are black.
1-10 Now push the front left side stop inwards and flush against
the vertical board and firmly tighten the clamp bolt nut.
Repeat operations 1-8 thru 1-10 at the right side of the jig. The
front and rear side stops are now indexed to provide accurate
board alignment in all routing procedures. You may now remove
the boards.
1-12 Make up a 3⁄4"x 6"[20 x 150mm] finger support board as
shown. Lengths: 11"[280mm] for Super12, 17"[430mm] for
Super18, and 23"[600mm] for Super24. This board will support
the guidefinger assembly in all front-clamping vertical board
modes. Clamp it in the rear of the jig.
Page 10
4
Chapter 1 Sup er Jig -12-18-24 User Guide
IMPORTANT
JIG ASSEMBLY, MOUNTING, AND USING THE CLAMPS
1
1
2
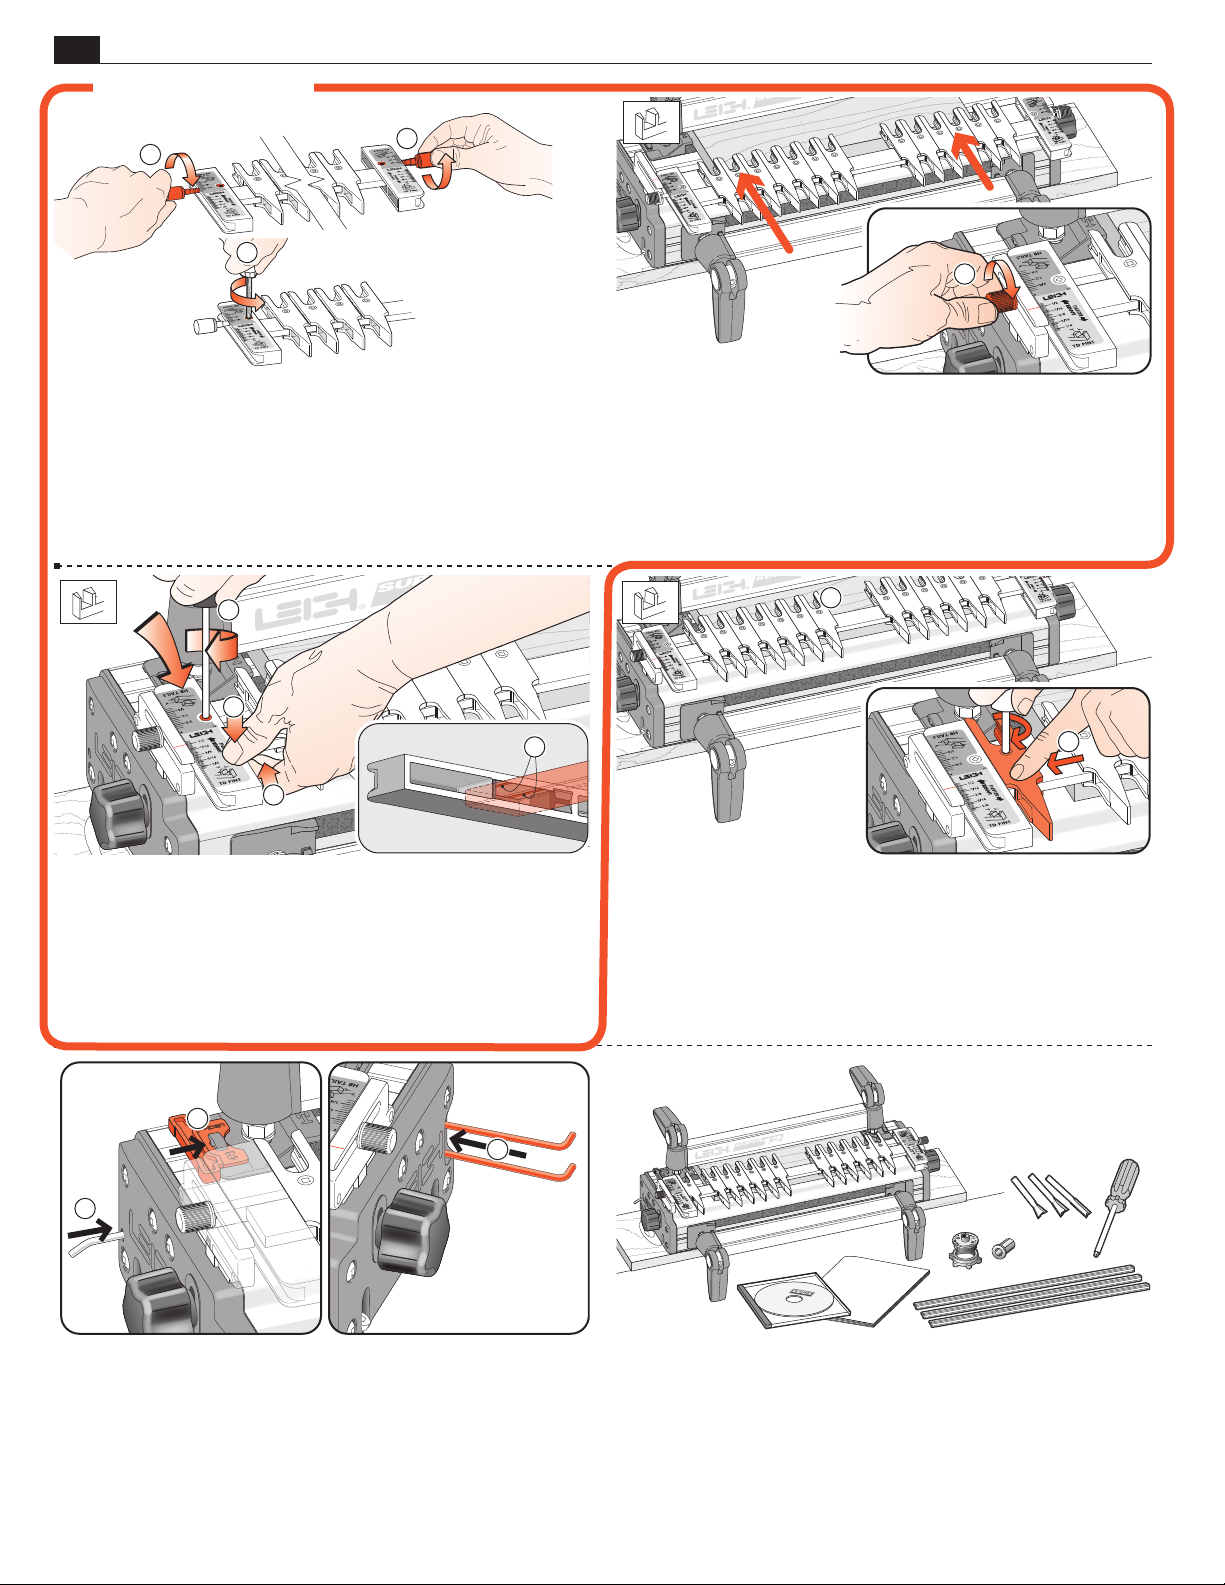
1-13 Before using the jig, the scales must be set into position on
the finger assembly. Install the two thumbscrews a few turns into
the scales . Loosen the scale lock screw at each end by one
turn only.
4
2
1
1-14 Slide the finger assembly onto the support brackets, in
TD Pin mode and set on the 1⁄2"[12,7mm] setting. First,
the
d
tighten both thumbscrews
.
Do not lower the assembly onto the finger support board.
1
3
1
1-15 Pull up on the finger bar while pushing down on the
to ensure the bar is touching the two registration pads
scale
inside the scale. Maintain pressure and tighten the scale lock-
➃. Repeat at the other end. To maintain correct finger
screw
assembly alignment, follow this procedure whenever you remove
the scales from the finger assembly.
1
3
2
2
1-16 With the finger assembly in dTD Pins mode , move the
outer end guidefingers to touch the scale block and lock in position . Note: the outer end guidefingers are used for router support
only. When guidefingers are loosened, the finger assembly should
easily slide on the support brackets. If not, apply a little candle
wax to the mating surfaces.
1-17 Finally, slip the Spacer on the outside of the left rear side
stop , the nylon stop rod through its storage hole in the left end
and the pin wrench in its slot in the right hand end housing .
1-18 With Superjig assembled and mounted, you have some
items left over:
1 Leigh jig user guide
1 DVD instruction video (English only)
1 Leigh e7-Bush and nut
2 Dovetail bits
1 Straight bit
1 Collet Reducer
1 square-head screwdriver
3 bridge-piece/crosscut extrusions
Page 11
JIG ASSEMBLY, MOUNTING, & USING THE CLAMPS
Chapter 1Sup er Jig -12-18-24 User Guide
5
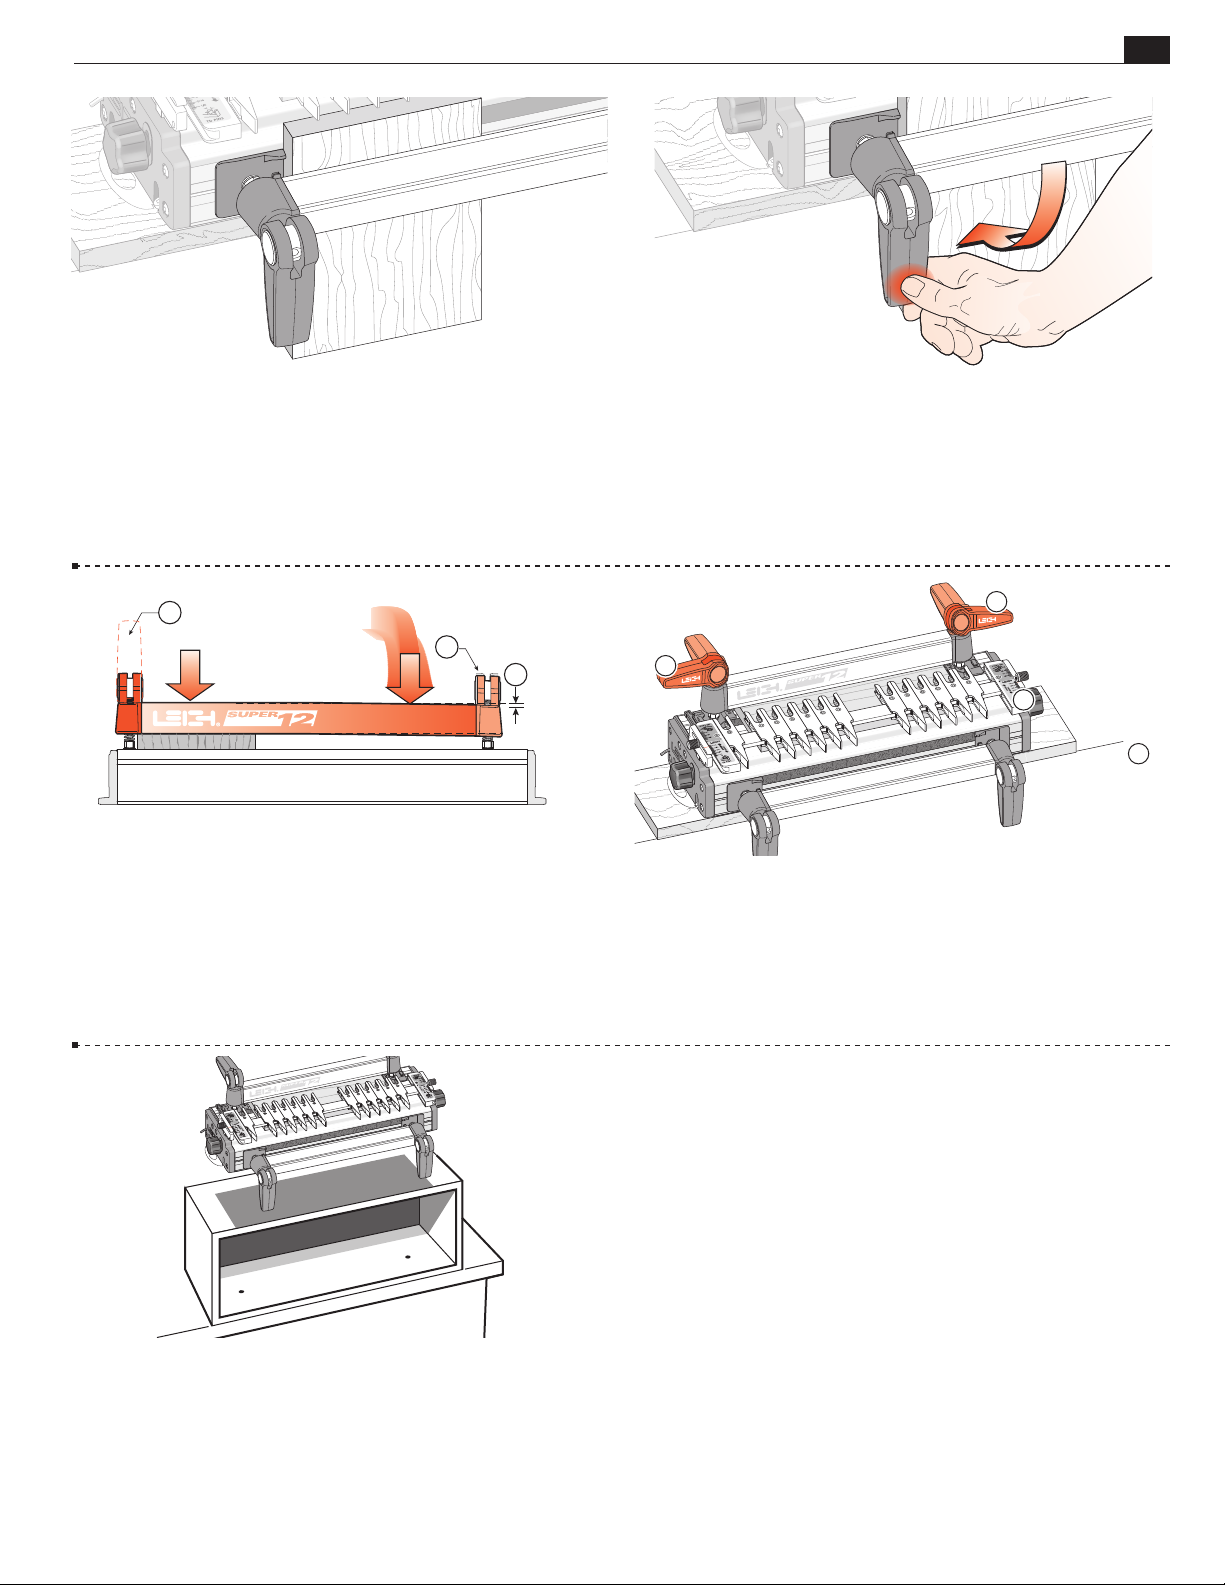
1-19 The Jig Clamps Use a piece of flat, even-thickness wood
to familiarize yourself with the jig cam clamps. You will operate
the cam-action speed clamps every time you use the jig, so get
used to the feel of the clamps first. Do not force the cam-action
speed-clamp. It has great leverage, and excessive force may damage
the workpiece or the jig.
1
2
3
1-21 For all but the wider workpieces, you need only operate the
clamp on the workpiece end of the jig to release the board . For
narrower boards, the clamp at the free end should be just tight
1
enough to bow the clamp bar about
⁄16"[2mm] .
1-20 A smooth, firm action is enough to engage the clamp.
Rule of thumb: If you can't throw the lever by pressing the end
of it firmly with your thumb, reduce the tension. Firm thumb
pressure is about right. A few minutes of trial and error will help
you feel the right clamp tension.
2
2
1
1
1-22 When engaged, the front clamp levers should normally point
down and the rear levers should point away from the operator
or up to 90˚ either side as required to obtain the optimum
clamping pressure.
1-23 To gain height for a more comfortable working position
or for routing longer boards, mount the jig to a box that can be
bolted securely to a bench.
See also 15-13.
■
Page 12
6
Chapter 1 Sup er Jig -12-18-24 User Guide
JIG ASSEMBLY, MOUNTING, AND USING THE CLAMPS
Page 13
7
SUPERJIG - CHAPTER 2
Adjusting the
Finger Assembly
1
1
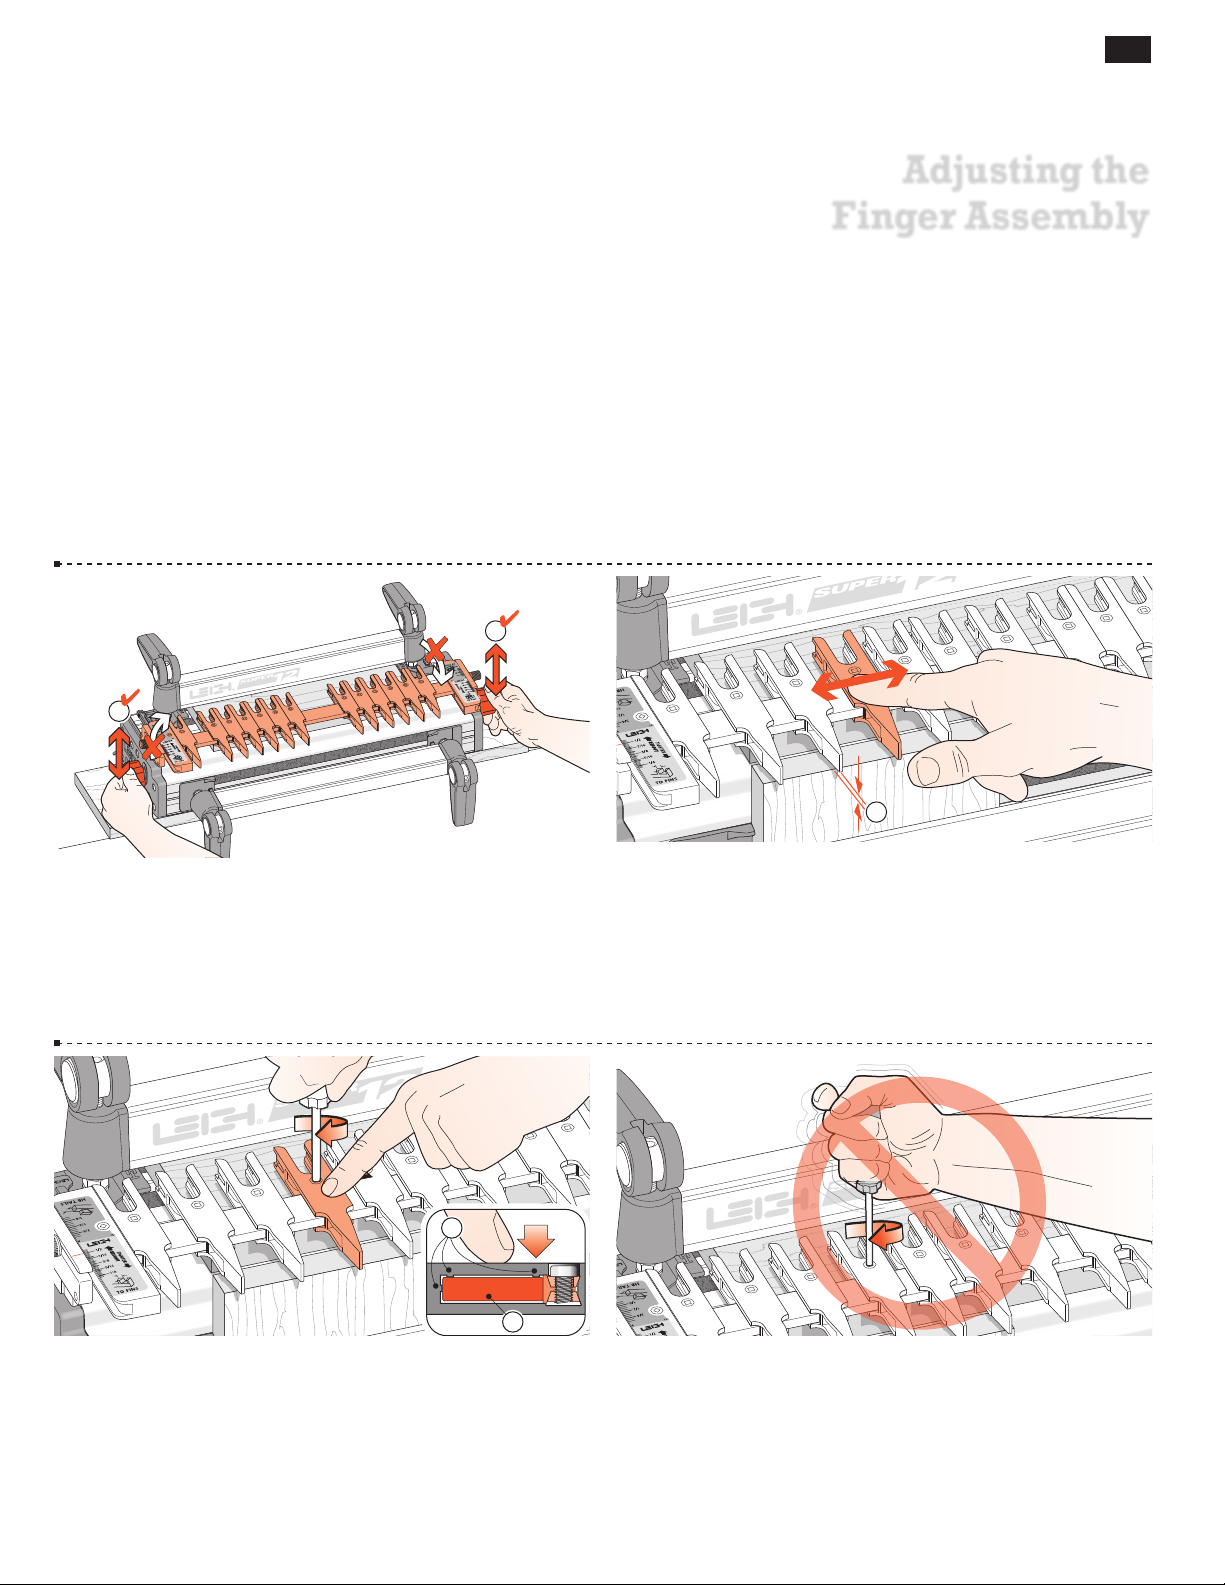
2-1 Practice with the finger assembly height adjustment. Loosen
the support bracket knobs and hold them firmly. Raise and lower
the assembly evenly, keeping it level
lock it at various heights. Do not raise or lower only one end of
the finger assembly.
, and tighten the knobs to
1
2-2 To practice adjusting the guidefingers, put a board in the front
clamp. Always raise the finger assembly slightly, approximately
1
⁄16"[2mm] above the spacer board and/or workpiece . This is
essential to allow the guidefingers to move freely on the guidefinger
bar and ensures that the fingers will be level and flush when locked
up. Move the guidefingers by pushing on the middle to slide them
along the guidefinger bar.
1
2
2-3 Loosen about half the guidefingers and practice unlocking, moving, positioning and re-locking them. Always press on
the center of the guidefinger when tightening the screws. This
ensures that the small pads on the inside of the finger contact
the face of the finger bar and keeps all the fingers level.
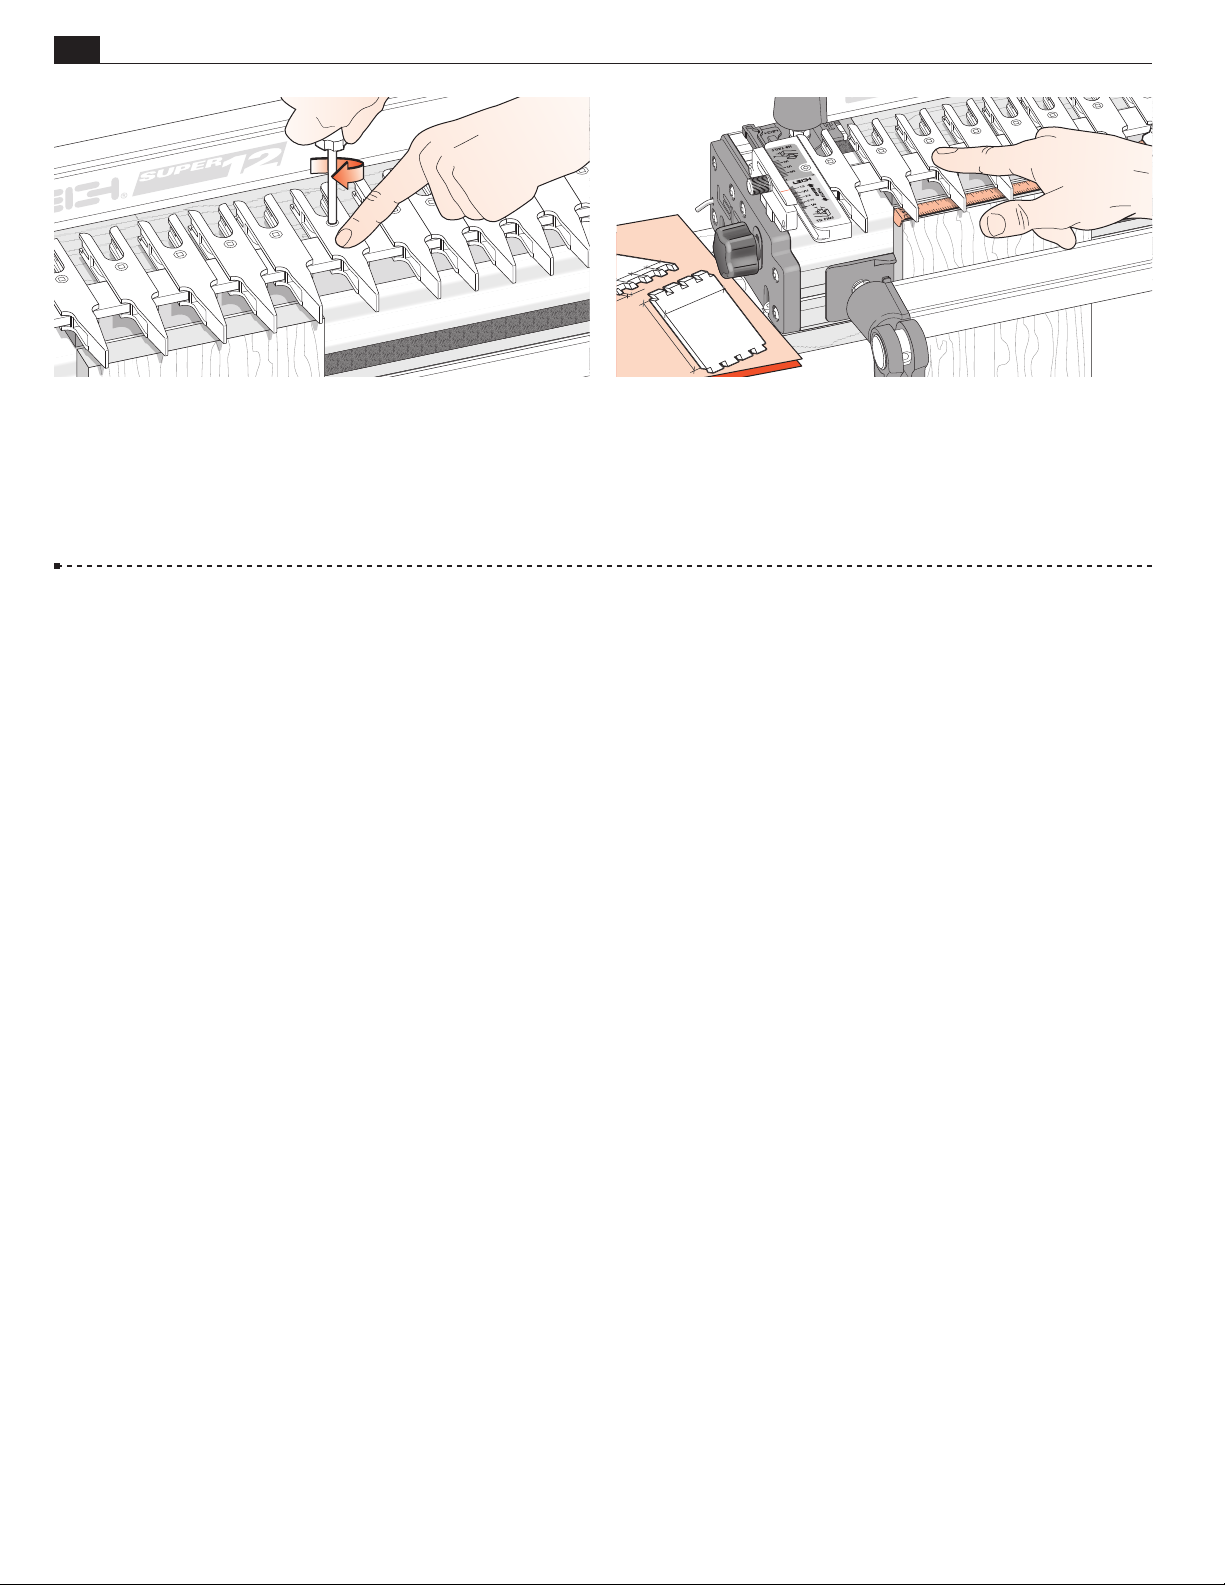
2-4 Do not over-tighten the guidefinger lock screws. The Leigh
screwdriver provided will give ample torque for easy lock-up without strain.
Hint: Fingertip tighten a loose screw until the slightest resistance is
felt. Do not tighten the screw more than half a turn (180˚) from the
first contact.
Page 14
8
Chapter 2 Sup er Jig -12-18-24 User Guide
ADJUSTING THE FINGER ASSEMBLY
4
3
3
3
1
3
2
3
1
3
2
1
31
30
9
2
1
1
28
7
2
0
6
1
2
25
9
4
2
3
2
2
8
0 21
2
9
1
7
8
1
7
1
6
16
5
1
14
5
3
1
2
1
4
1
1
0
1
3
9
8
7
2
6
5
1
4
3
2
1
3/4"thick
20"
2-5 Always tighten unused guidefingers before routing, as
router vibration may cause loose screws and finger lock parts to
fall out and be lost.
2-6 You can adjust the guidefingers by eye, or by measurement
to suit a set of plans.
■
Page 15
SUPERJIG - CHAPTER 3
These images were copied from D4R Pro UG Fig’s 8-42 and 3-2
The Leigh e-Bush and
Optional Guidebushes
The guidebush is the vital link between router and jig. All joints created on a Superjig are routed with the unique
e7* elliptical guidebush, a Leigh innovation that provides precise joint fit adjustment for box joints and sliding dovetails.
If your router doesn’t accept the e7-Bush, you can use an alternative guidebush with some limitations.
*Supplied with each Superjig. U.S. Patent No. 8, 256,475. UK Patent No. GB2443974. Patent Pending in Canada.
9
7
16
"
[~11,1mm]~
/
1
4
"
min.
/
[6,35mm]
1 2
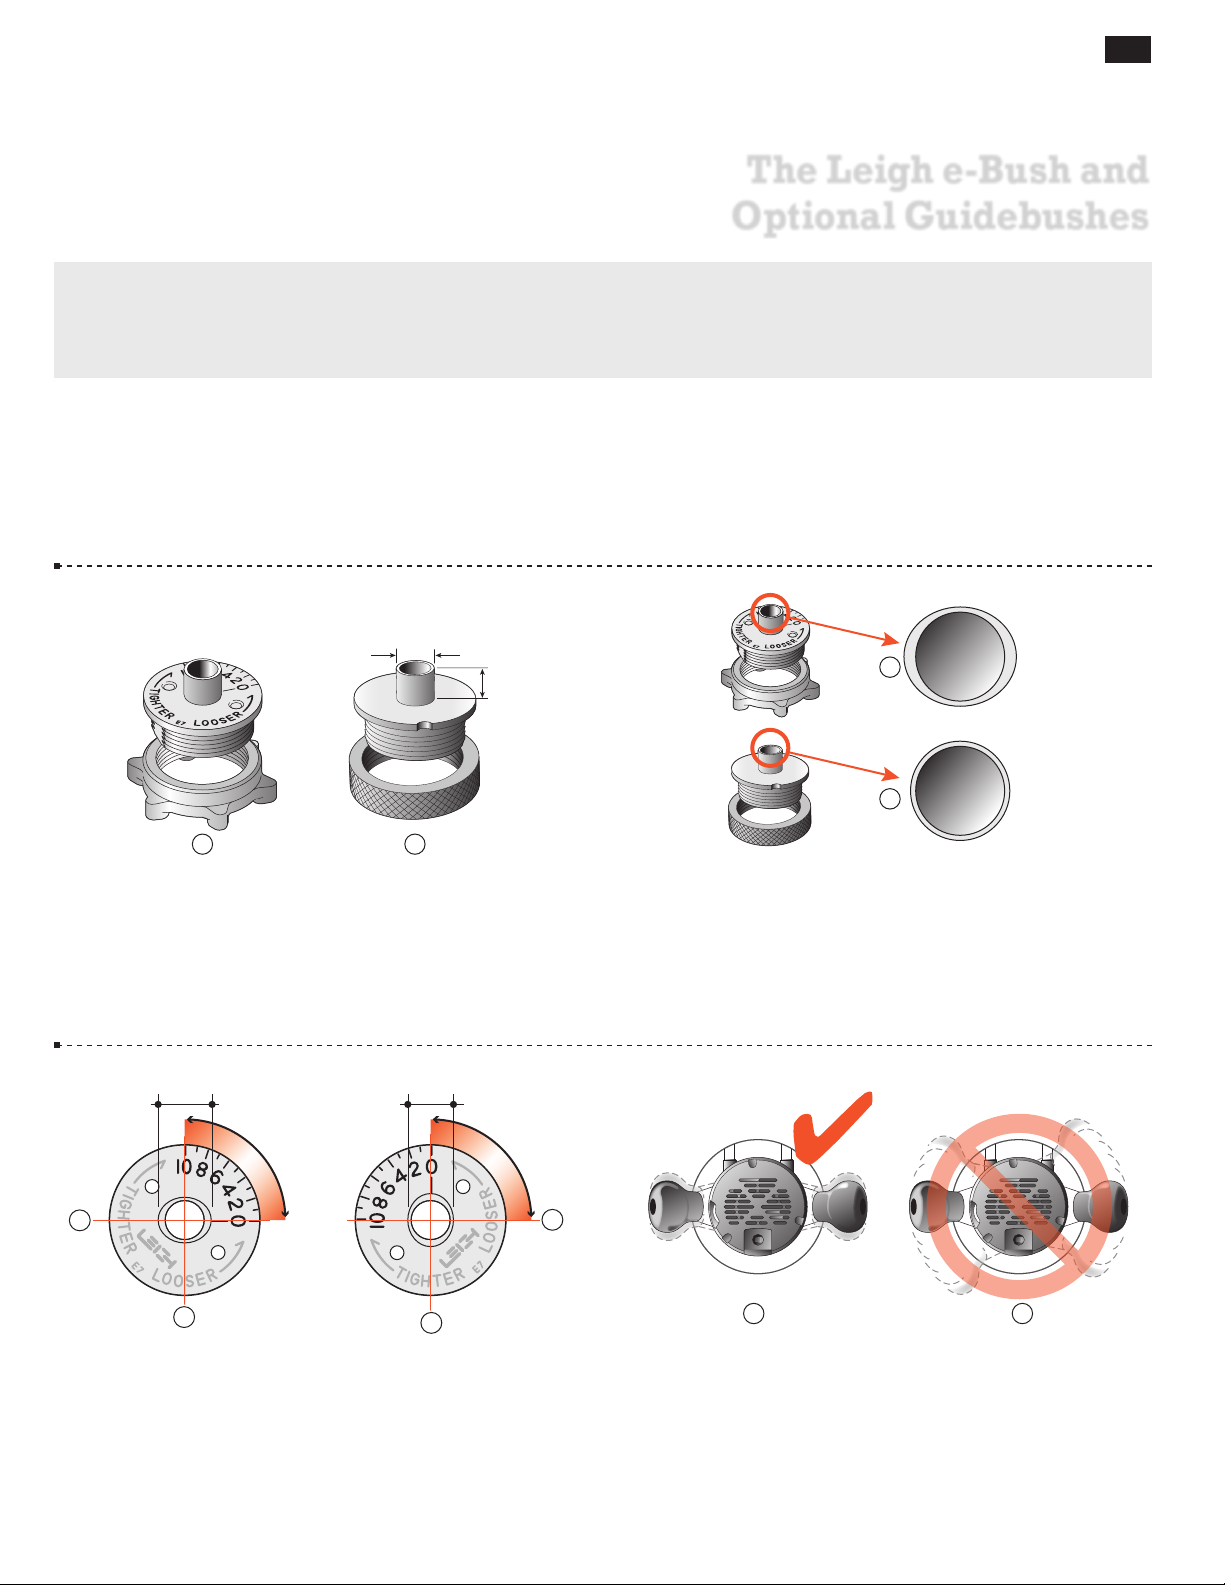
3-1 The Leigh e7-Bush is used to rout through, half-blind,
single pass half-blind and sliding dovetails on a Superjig. The
elliptical design provides precise joint fit adjustment for box joints
7
and sliding dovetails. A round ~
1
barrel length
/4"[6,35mm]), can be used to rout through, half-blind,
/16"[11,1mm] guidebush (min.
and sliding dovetails on the Superjig, but the e7-Bush is superior.
~7⁄16"[~11mm] ~7⁄16"[~11mm] less .020"[,5mm]
1
2
2
1
3-2 The Leigh e7-Bush that comes with your Superjig is a
unique template guidebush that is adjustable in size. Unlike regular
circular template guidebushes , the e7-Bush is slightly elliptical
in cross section . This simple innovation effectively changes the
guidebush “active diameter size” when it’s rotated, and provides
benefits not possible with a standard round guidebush.
2
1
3-3 The e7-Bush (~7/16") fits the router base or a guide bush
adaptor in the base (see Appendix I). The ellipse/oval shape has
a major axis ~7/16"[11,1mm], and minor axis ~7/16"[11,1mm]
less .020"[,5mm]. Turning the e-Bush 90 degrees in the router base
changes the active diameter by .020"[,5mm] providing minute
adjustment and recordable settings for perfectly fitting box joints.
1 2
3-4 Here’s how it works. In normal use on a dovetail jig, the
operator does not rotate the router more than a few degrees either
way . In fact, because of potential bit-to-bush eccentricity problems it is advisable to minimize router rotation on jigs .
Page 16
10
Chapter 3 Sup er Ji g-12-18-24 User Guide
1
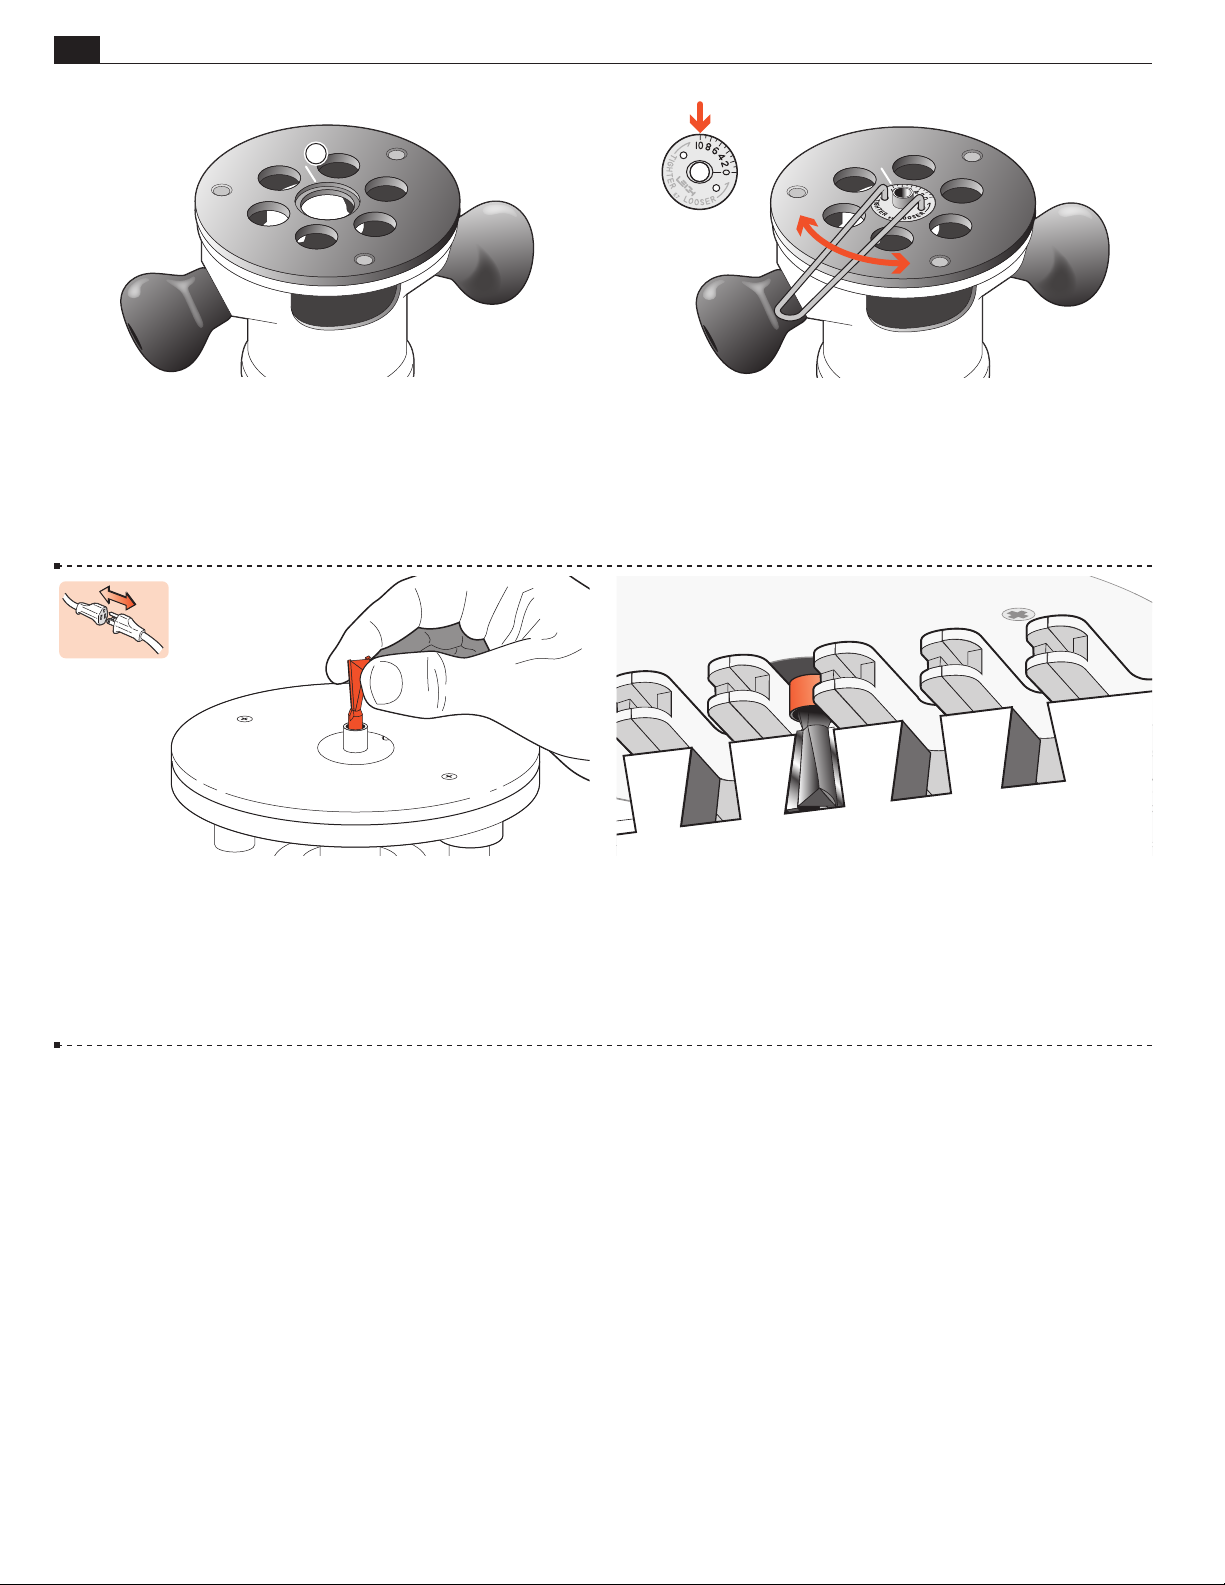
THE LEIGH e-BUSH AND OPTIONAL GUIDEBUSHES
3-5 Establish the orientation in which you normally hold and
operate the router on the jig. Now, up-end the router in the same
orientation. Make a small scratch line or permanent ink mark on
the router base or e-Bush adaptor at the 12 o’clock position .
3-7 The bit goes through the guidebush and fits in the router
collet or chuck.
3-6 Fit the
e7-Bush to the router and align No.10 to the scratch
mark. The No.10 setting is used for all through and variably spaced
half-blind dovetails on Superjigs. Settings for single pass half-blinds,
box joints and sliding dovetails are described in applicable chapters.
Be sure to retighten the e-Bush nut after each adjustment.
3-8 The projecting part of the guidebush runs along the side
edge of the guide finger. The rotating bit cuts the wood only, and
touches neither the guidebush nor the guide surface.
■
Page 17
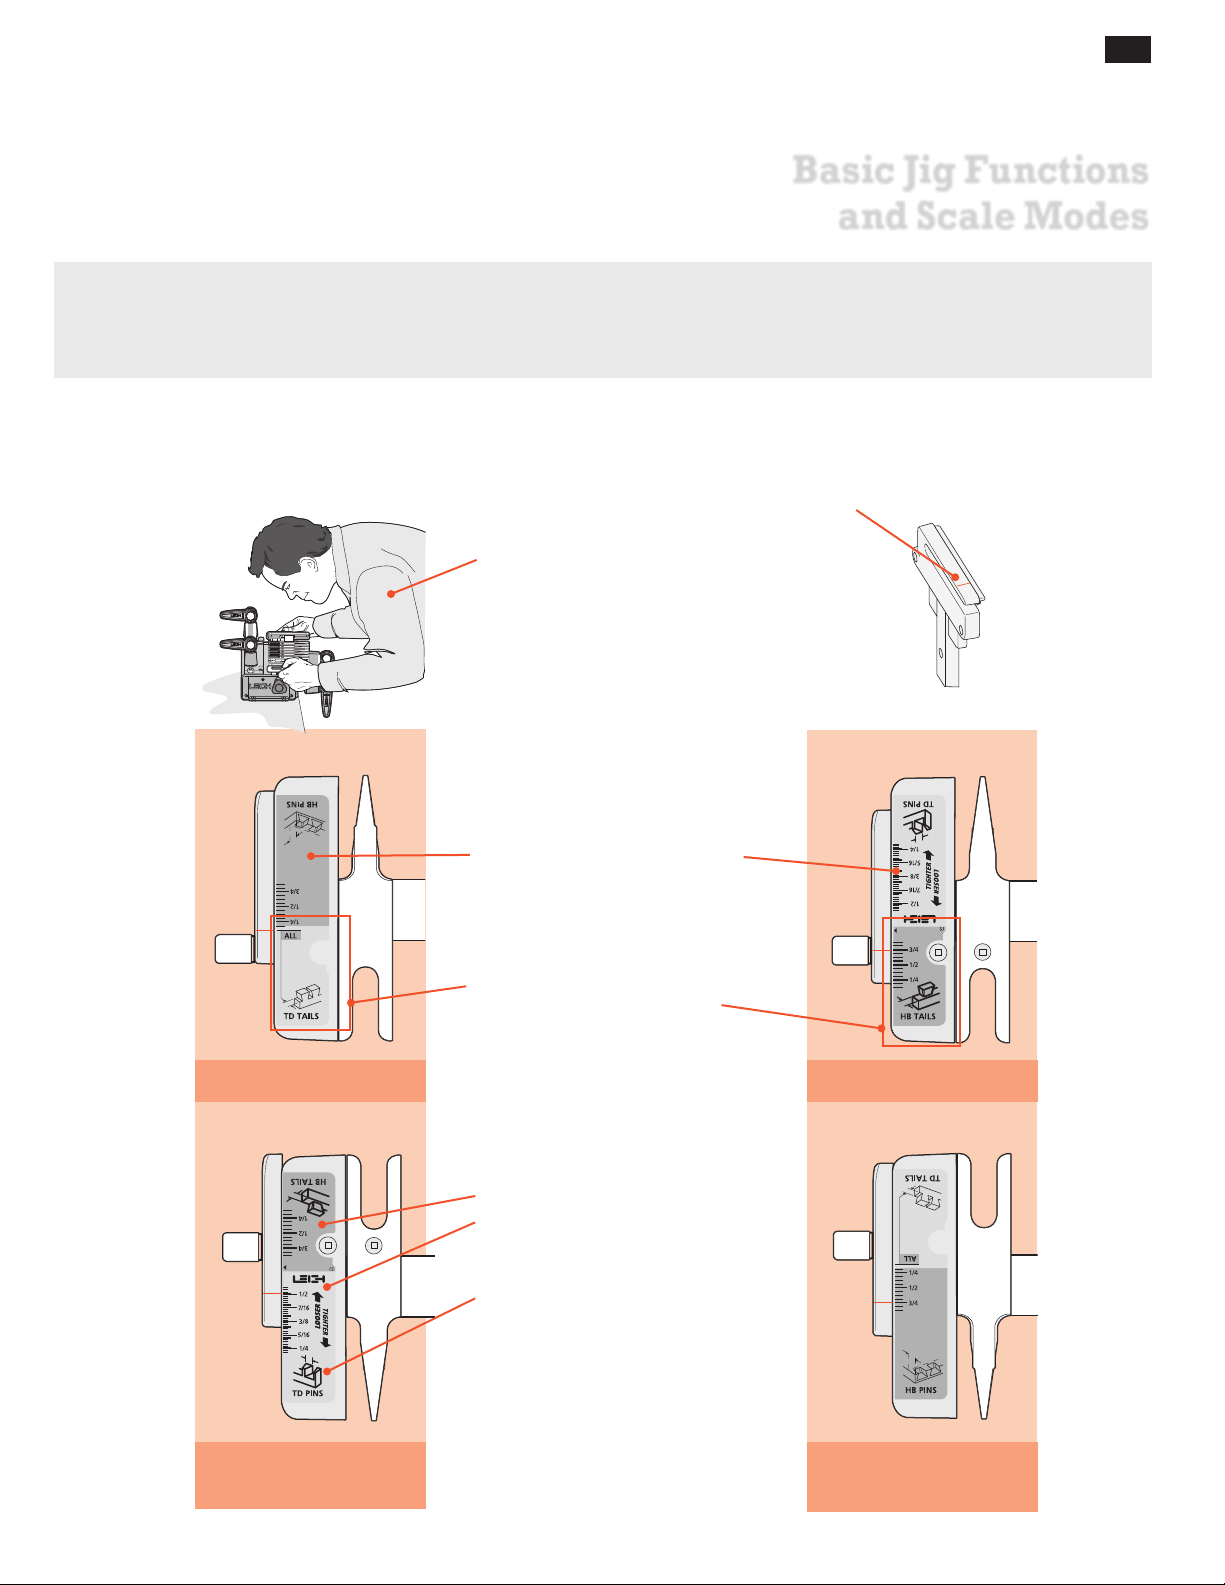
SUPERJIG - CHAPTER 4
Basic Jig Functions
and Scale Modes
Here are the basics for understanding the different Superjig dovetail modes and settings.
11
THE FOUR SCALE MODES
The Finger Assembly attaches to the support
brackets in four different modes to match the
type of joint you are cutting.
Reading scales
from directly
above helps
sight the lines
accurately.
Note: Inch scales are shown here.
Millimeter scales have similar
layouts.
The inactive scale is always on
the rear of each scale assembly
and is upside-down.
The active scale is always on the
front of each scale assembly.
This line is for the finger assembly
scales. The line is illustrated in red
for clarity in this user guide, but is
black on the jig.
1. TD TAILS
2. TD PINS
Scales are color coded.
• Green: Half-Blind Dovetails.
• Silver: Through Dovetails.
Each scale has its own mode icon
(a drawing of the joint part made
in that mode).
The specific settings for each scale
are fully described in the appropriate chapters.
3. HB TAILS
4. HB PINS
Page 18
12
Chapter 4 Sup er Jig -12-18-24 User Guide
BASIC JIG FUNCTIONS AND SCALE MODES
1
2
2
1
2
2
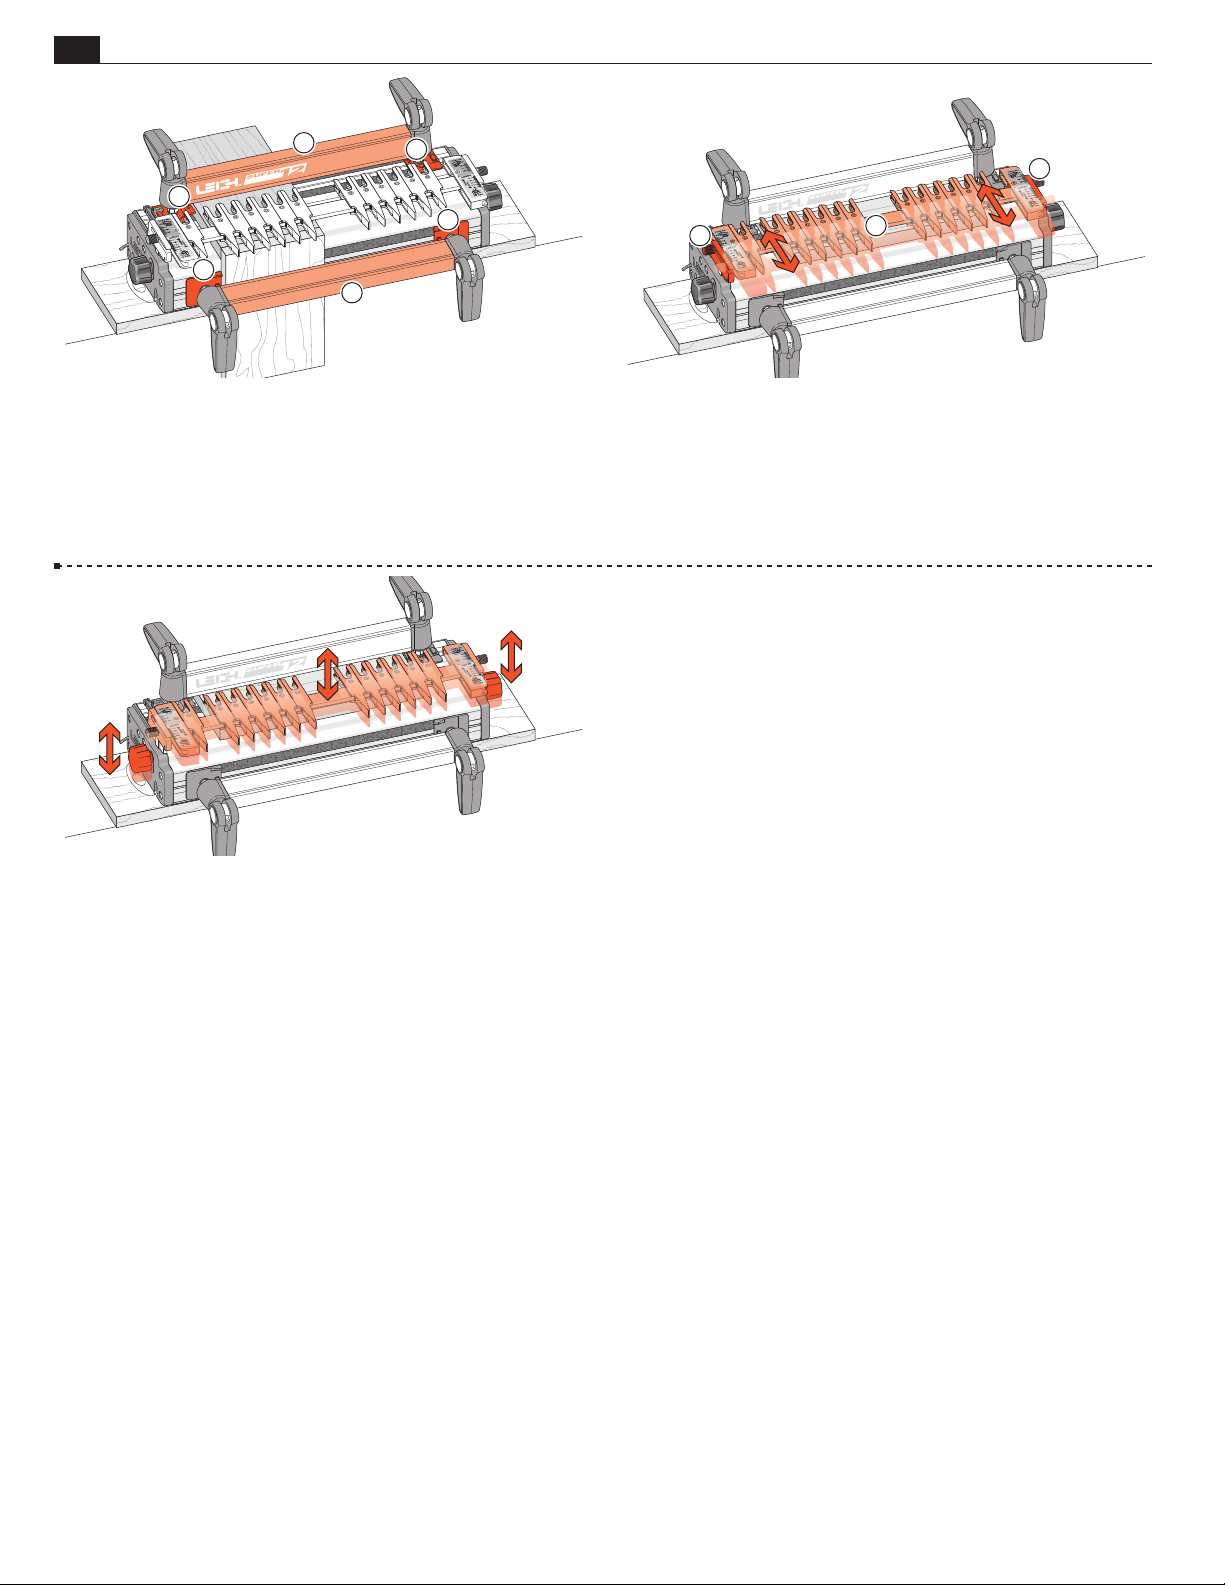
4-1 The two clamp bars hold workpieces horizontally or
vertically. The side stops align the boards in the correct position each time.
2
2
1
4-2 The guidefinger assembly slides in the support brackets
above the workpiece. The finger assembly is adjusted in or out
using calibrated scales on each end to suit different thicknesses of
vertical boards.
4-3 The finger assembly is raised or lowered using the support
brackets to suit different thicknesses of horizontal boards.
■
Page 19
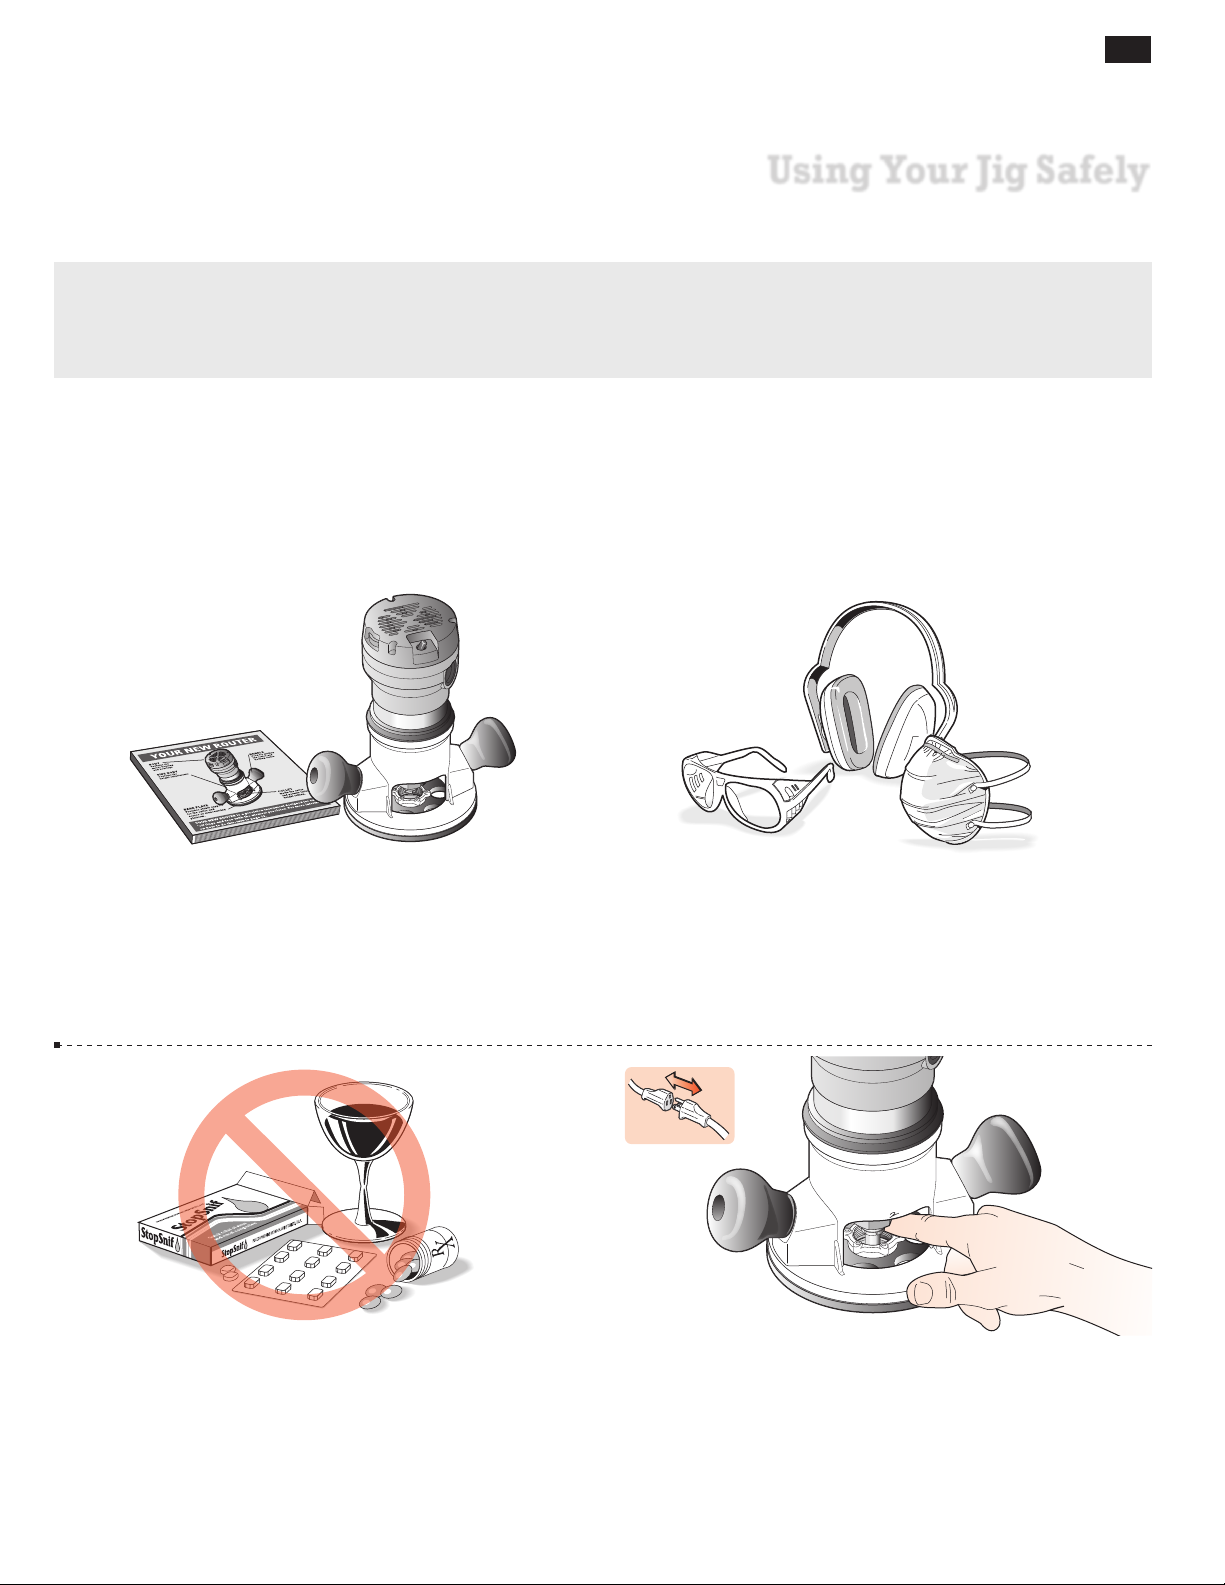
Safety is not optional.
Read and follow the recommendations in this chapter.
13
SUPERJIG - CHAPTER 5
Using Your Jig Safely
5-1 Read the user guide that came with your router. It is
essential to understand the router manufacturer’s instructions
completely. Always operate variable speed routers at the fastest
possible speed.
5-3
Never drink alcohol or take medications that may cause
drowsiness when you will be operating a router.
5-2 Always wear approved safety glasses.
Always wear hearing protection.
Protect yourself from harmful dust with a face mask.
For complete comfort and convenience, get yourself a Leigh VRS
(Vacuum & Router Support) to match your jig model.
5-4 Always disconnect the power source from the router when
fitting bits or guidebushes, or making adjustments.
Before connecting the router to the power source, make sure the
bit and collet revolve freely in all the areas you plan to rout, and
the bit does not touch the guidebush or jig.
Page 20
14
Chapter 5 Sup er Jig -12-18-24 User Guide
USING YOUR JIG SAFELY
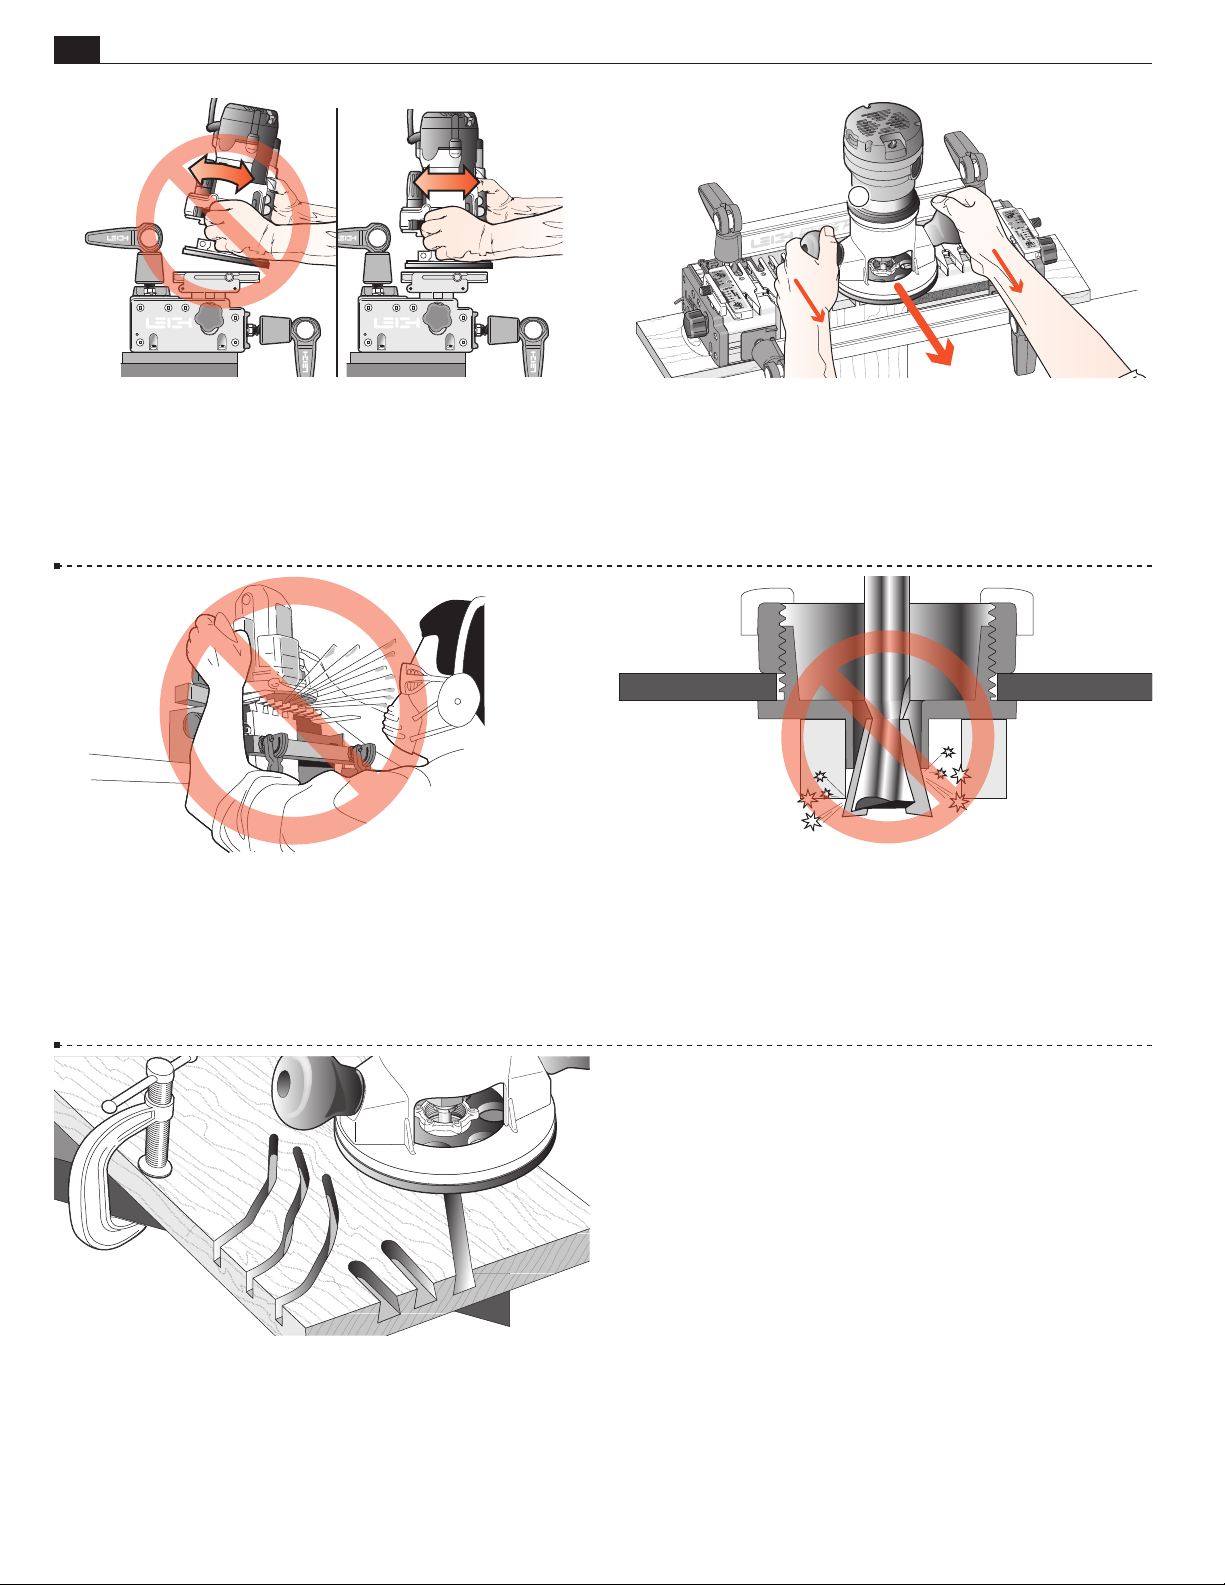
1
5-5 Do not tilt the router on the jig.
Keep the router flat on the jig assembly.
Note: The optional Leigh VRS attachment prevents router tilting.
5-6 If you insist on removing the router from the jig while it
is still revolving, always pull it straight off the jig horizontally,
and do not raise or lower the router until it is completely clear
of the jig.
5-7 Do not rout at face level. 5-8 Never release the router plunge mechanism when using
dovetail bits. Check if your plunge router has a stop nut to prevent
this from happening accidentally.
5-9 If you have never used your router before, be sure to follow
the router manufacturer’s instructions for its use. Make plenty
of simple open-face practice cuts without a guidebush before
you try to use the router on the Leigh jig. You must, of course,
always use a guidebush when routing on the Leigh Jig.
■
Page 21
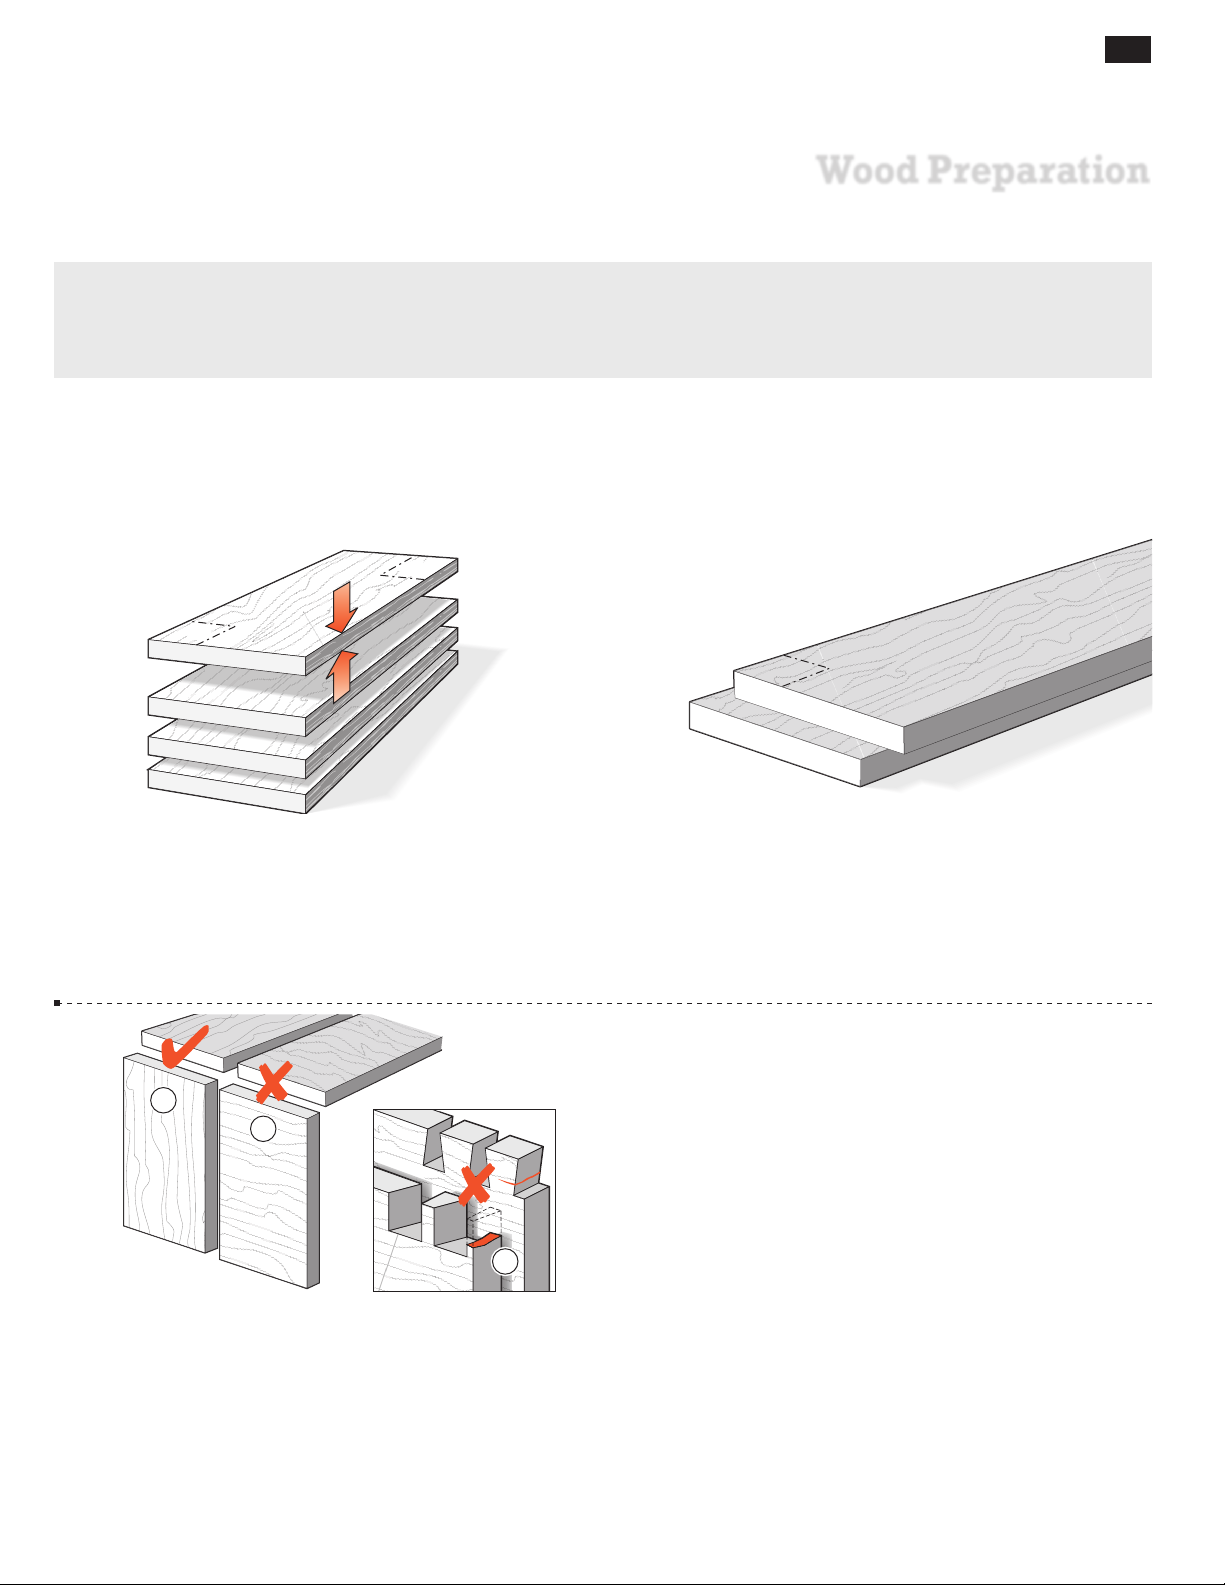
"Garbage In - Garbage Out"...
This adage of the computer age stands equally true for dovetail jigs.
90°
15
SUPERJIG - CHAPTER 6
Wood Preparation
90°
6-1 It is vital for accurately aligned joints that stock used on the
Superjig should be prepared straight, flat, of even thickness and equal
widths, with square ends and edges. Note that plywood is generally unsuit-
able for routing because of tearout problems.
1
2
90°
6-2 You will want to test the jig, so prepare some 3⁄4" x
1
⁄2"[20x140mm] boards. Cut them to length as you need them
5
for the jig tests you want to perform. Use them for practice with
the jig’s various joint modes so you can see how the different
modes work. Remember, though, that two boards of different
thicknesses can be joined just as easily.
3
6-3
Dovetail joints are intended for joining end-grain
to end-grain . Attempting to cut dovetails in side-
grain does not work because:
A. The wood will tear out badly when routing.
B. Even if you could rout them, the pins and tails would easily
break off across the short grain , either during or soon after
the assembly when the boards start expanding or contracting
at different rates.
■
Page 22
16
Chapter 6 Sup er Jig -12-18-24 User Guide
WOOD PREPARATION
Page 23
17
SUPERJIG - CHAPTER 7
Router Preparation
1
1
1
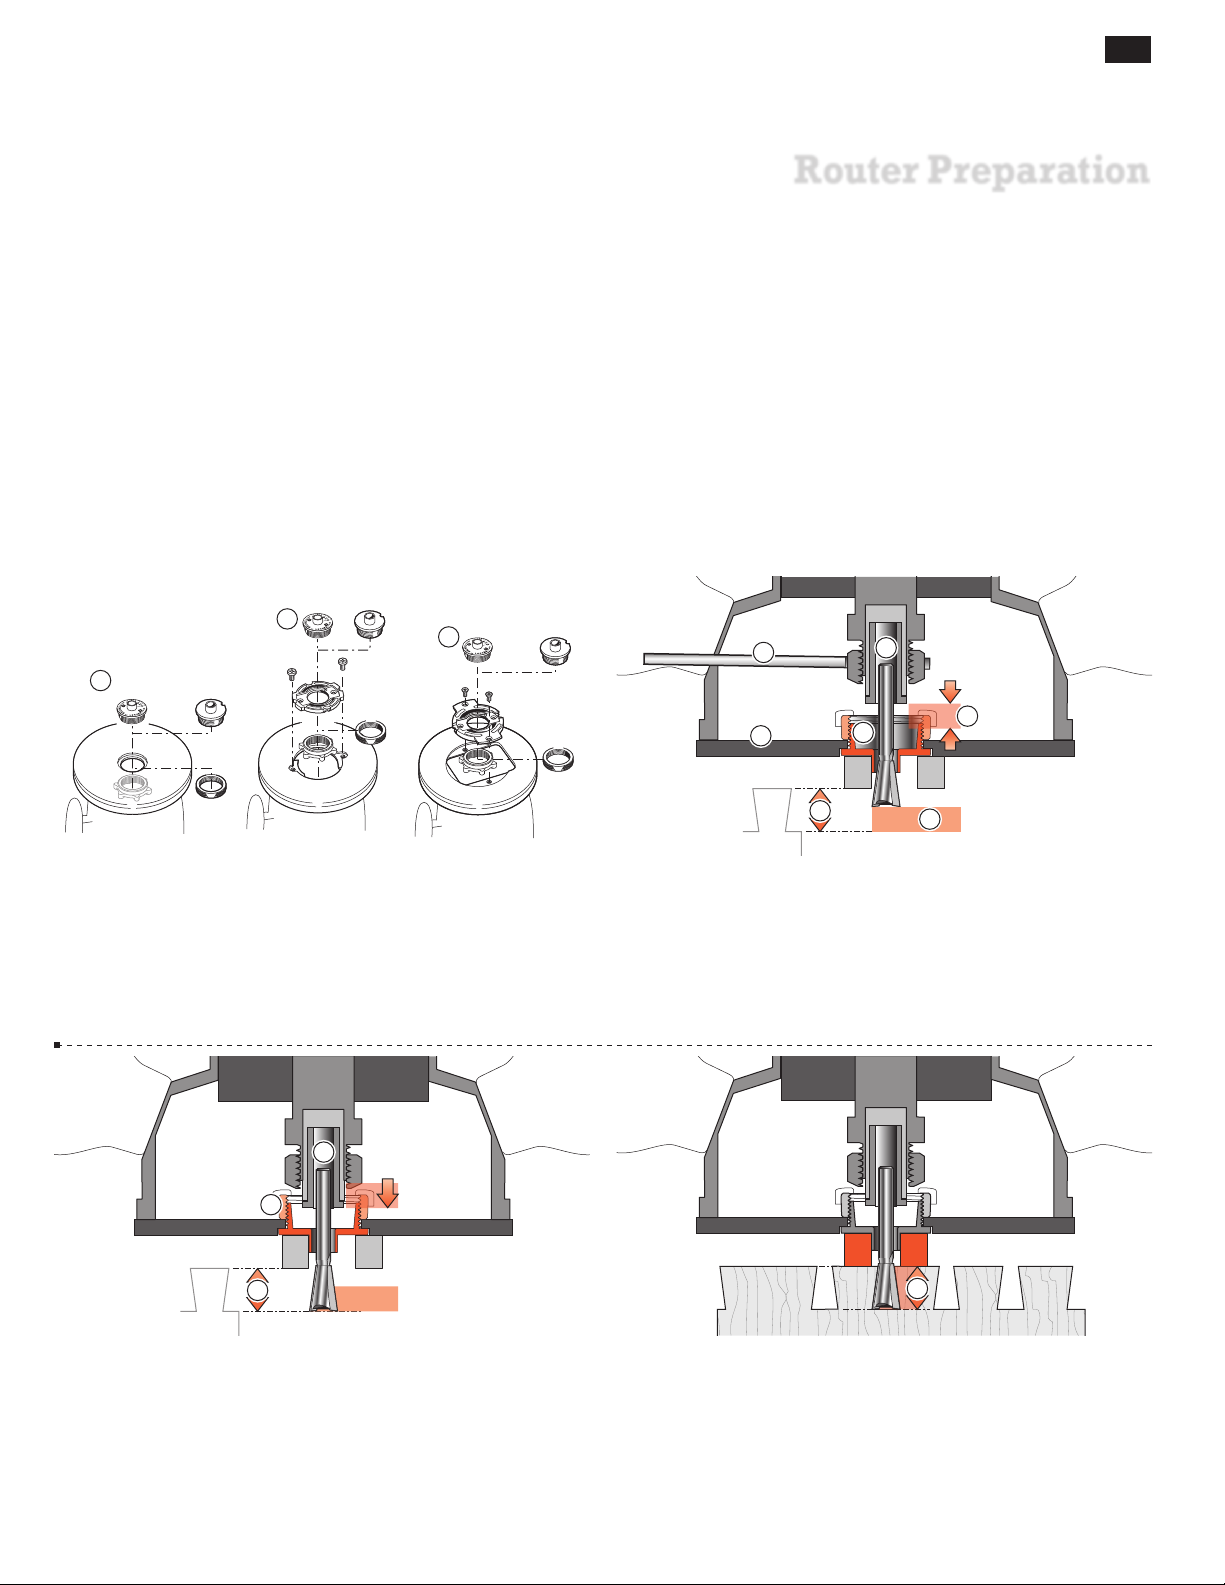
7-1 Fit the e7-Bush . One is included with your Super Jig.
Some guidebush adaptors may have to be modified to allow adjustment rotation of the
If the e-Bush is incompatible with your router, any
guidebush (min. depth
e7-Bush in the base. See page 67.
7
/16[11,1mm]
1
/4" see page 67) will work for all but box
joints on the Superjig.
2
3
1
6
2
4
5
4
7-2 When fitting a bit to the router , fit the shank as far into
the collet
as possible. Always rout with the collet as close to the
guidebush as possible. Usually you can't securely grip the collet nut
with a wrench if the collet is at its optimum low position. Fit the
bit so that the remaining travel ➃ between collet and guidebush
➄
will let the bit reach the required depth of cut .
5
6
7-3 Tighten the collet securely and lower the collet to adjust
the depth of cut , but make sure the collet does not contact the
guidebush ➄.
1
7-4 Depth of Cut: The depth of cut always refers to the actual
depth of the cut into the wood beneath the guidefingers .
Page 24
18
Chapter 7 Sup er Jig -12-18-24 User Guide
ROUTER PREPARATION
2
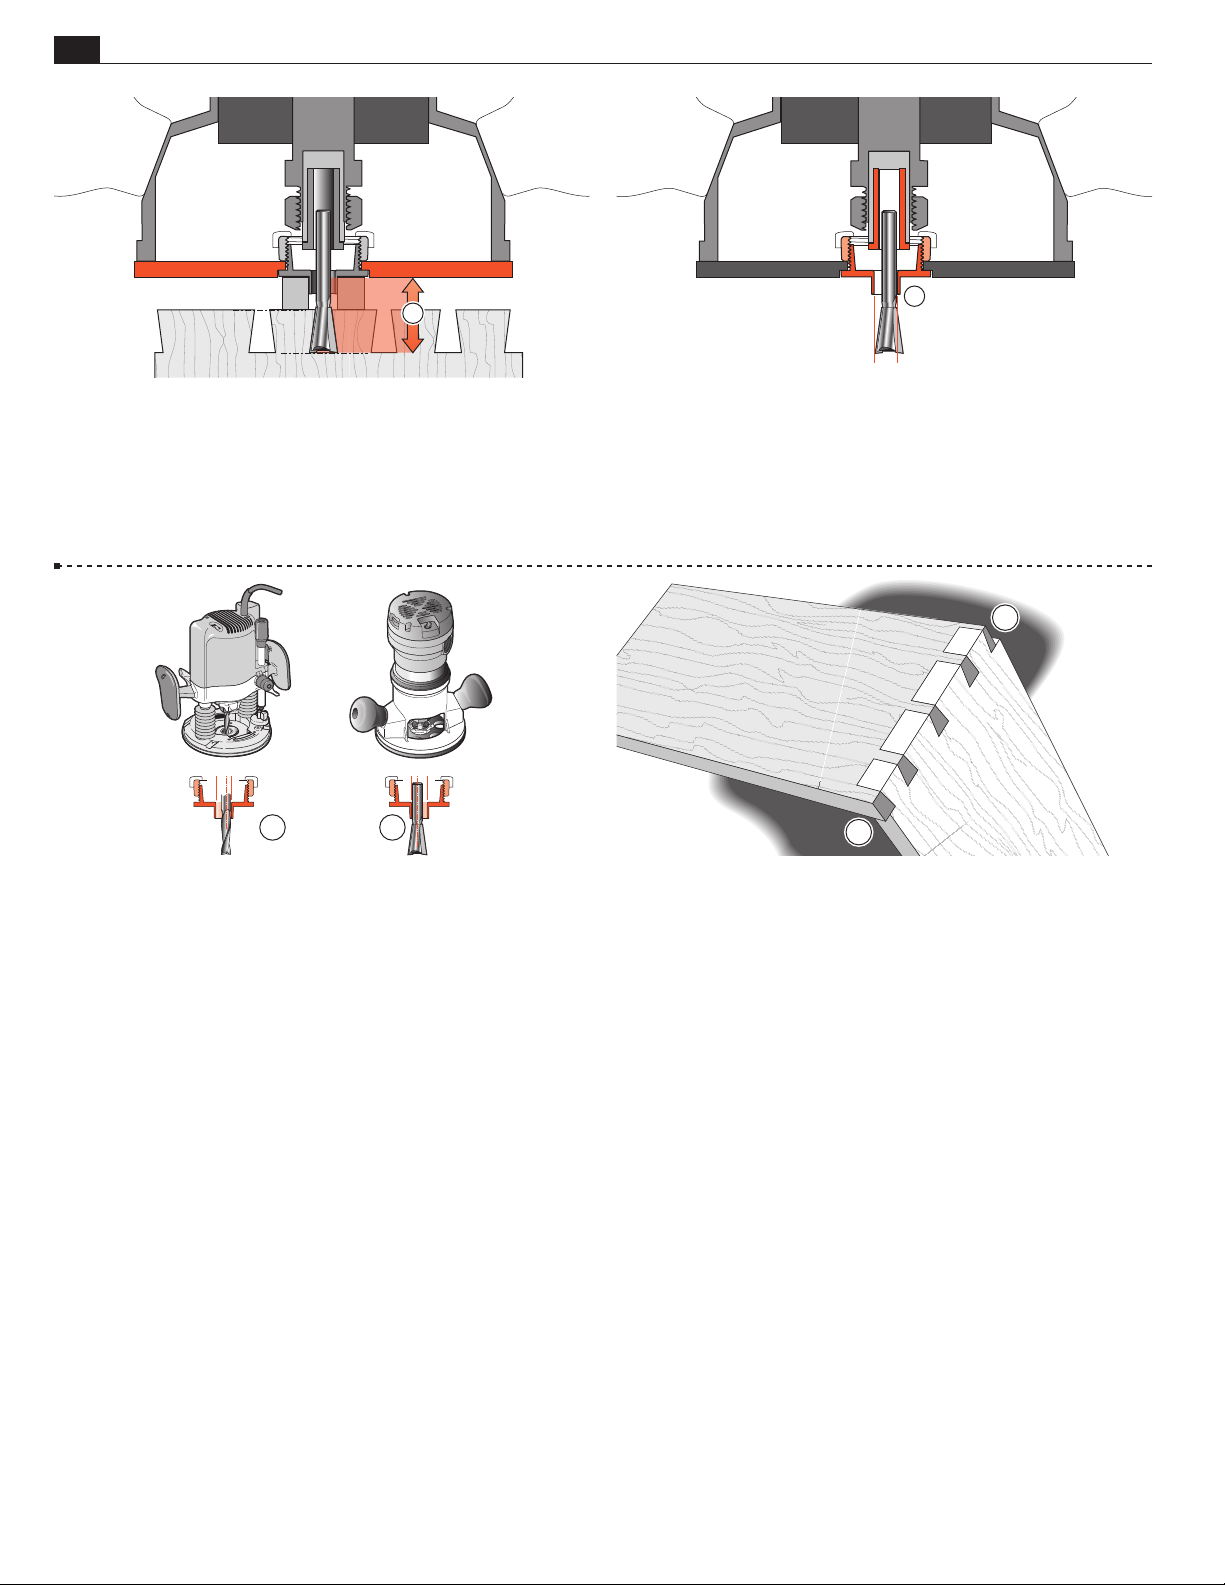
7-5 Depth of cut is not the distance the bit projects from the
router base. This is bit projection
. This user guide generally
refers to depth of cut. Bit projection is always .500"[12,7mm]
more than depth of cut.
22
1
7-6
Ideally, the router collet (and bit) should be concentric (centered) to the guidebush as in figure 7-5. Regrettably, this is often not
the case; the bit can be off center (eccentric to) the guidebush . The
illustration shows the problem highly exaggerated. The good news:
bit to bush alignment doesn’t affect joint fit or flushness; both are
“adjusted out” in normal jig setup.
3
3
7-7
Concentricity problems can only arise if two routers are used for
through dovetails, (one for pins; one for tails). Routers with different
bit to guidebush offsets (misalignment shown highly exaggerated)…
7-8
…will cause pin to tailboard
misalignment (again, shown
highly exaggerated).
Fortunately, some newer routers have sub-bases that can adjust
for concentricity. If you don’t have this type, it might pay to stick
to a single router for through dovetails.
■
Page 25
19
SUPERJIG - CHAPTER 8
Through Dovetail
Procedures
In these instructions for using the Leigh Superjig dovetail Jig, we recommend using certain bits and board sizes
just because they are easy to work with. When you have cut some practice joints and gained confidence in your
ability to get the results you want, feel free to use the bit selection charts in Appendix II to plan whatever dovetail
routing you need for your projects.
Concept of Jig Operation – THROUGH DOVETAILS
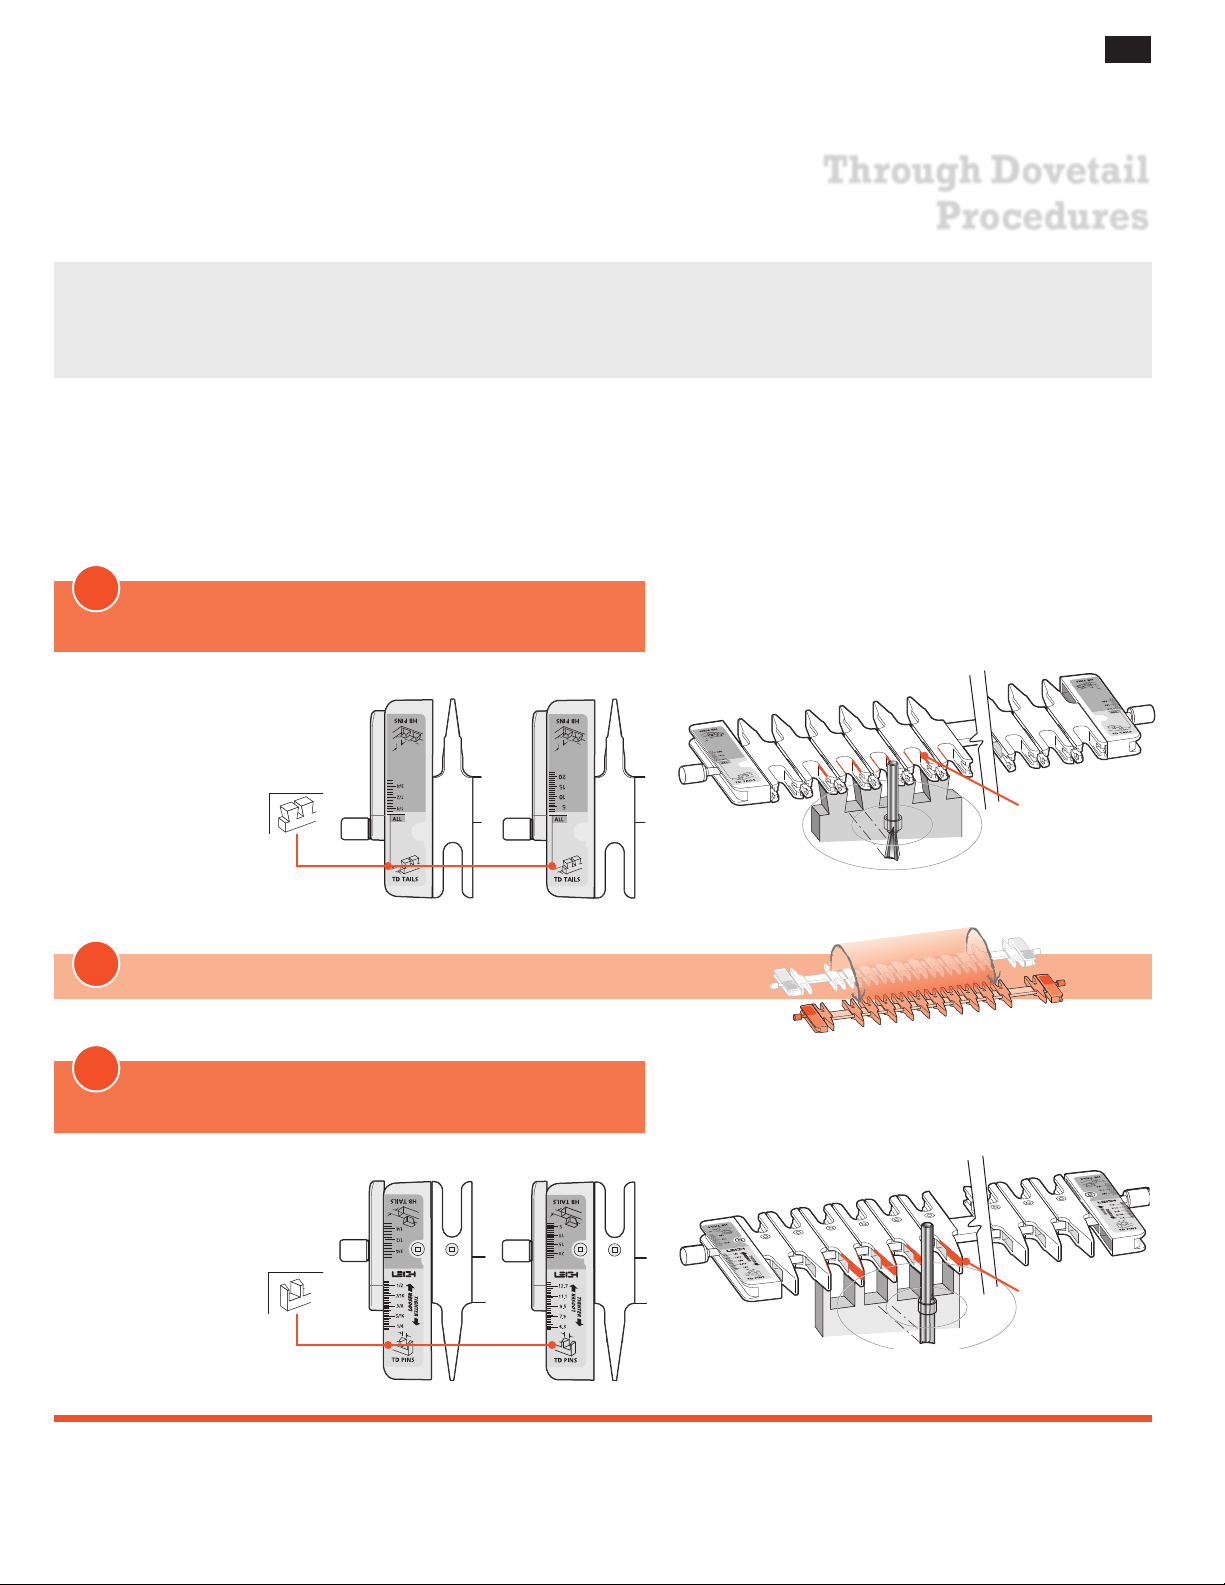
Start with the Finger Assembly in the D TD TAIL mode and follow these steps on your jig. Grasping the simple basic concept of
operation will now greatly assist you in understanding the instructions. Note that the active guide surface (against which the guidebush
runs) is indicated in red in these illustrations.
1
Start in
Through Dovetail Tails (TD TAILS) mode
MODE ICONS
Illustrations in this user
guide include the correct
mode icon for the current instruction. The
icons are also used in
the instruction text.
2
ROTATE the finger assembly toward you 180°
3
Now the Finger Assembly is in
Inches
Through Dovetail Pins (TD PINS) mode
Inches
Millimeters
Active
Guide Surfaces
TD TAILS
TD PINS
Millimeters
Active
Guide Surfaces
Page 26
20
Chapter 8 Sup er Jig -12-18-24 User Guide
2
5
4
1
6
3
THROUGH DOVETAIL PROCEDURES
8-1 Through Dovetail Terminology:
Pins
Pin sockets
Half-pins
Half-pin sockets
Tails
Tail sockets
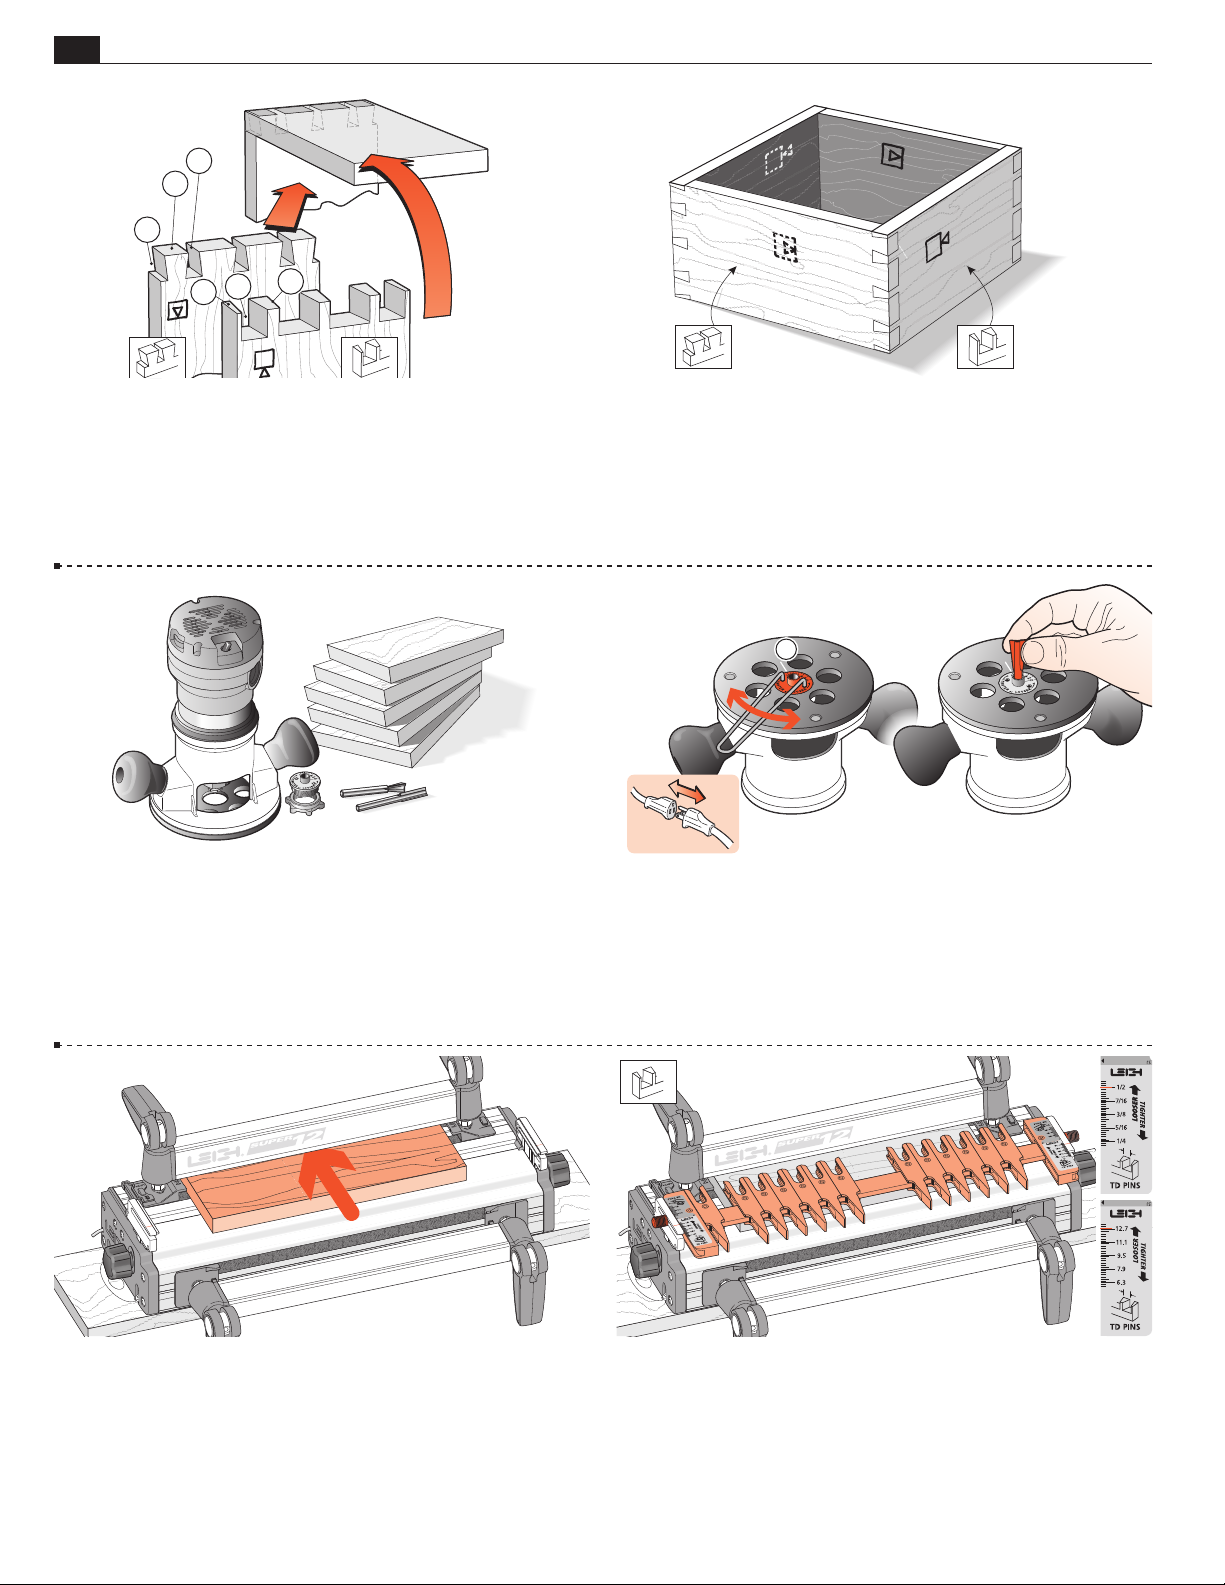
The pins fit in the pin sockets. Joints should almost always end
each side with half-pins.
8-3 For this trial you need five identical boards 3⁄ 4"x
1
⁄2"[20x140mm] x about 8"[200mm] long. Mark inside faces for
5two tailboards and outside faces for three pinboards (one pinboard is
1
a spare). Use the e7-Bush, the No. 80-8
5
bit and 140-8
13
Note:
⁄16 "[7,9mm] straight bit (all included with Superjig).
⁄16 "[20mm] is maximum through pin board thickness.
⁄2"[12,7mm]x 8° dovetail
8-2 Let’s look at how to make a simple square box. When you
assemble the finished pieces with the faces properly oriented, then
any one of the pin ends will fit any one of the tail ends. In fact,
the box can be put together in six different ways.
1
8-4 Fit the E-7 guidebush to the router. Align the No. 10 mark
with the base mark . No guidebush adjustment is required with
through dovetails. If you have a router that is incompatible with
7
the e-Bush, you can use a standard
1
depth
⁄4" see page 67) for through dovetails.
⁄16"[11,1mm] guidebush (min.
Then fit the supplied 80-8 dovetail bit to the router.
8-5 Clamp the finger support board in the rear clamp. 8-6 Place the finger assembly on the support brackets in
the dTD PINS mode, flat on the spacer board, and with the
1
scale set on the
⁄2"[12,7mm] setting for now. Don’t worry about
the scale’s specific meaning now. Each scale’s use will be fully
explained in the appropriate section.
Page 27
THROUGH DOVETAIL PROCEDURES
Chapter 8Sup er Jig -12-18-24 User Guide
1
21
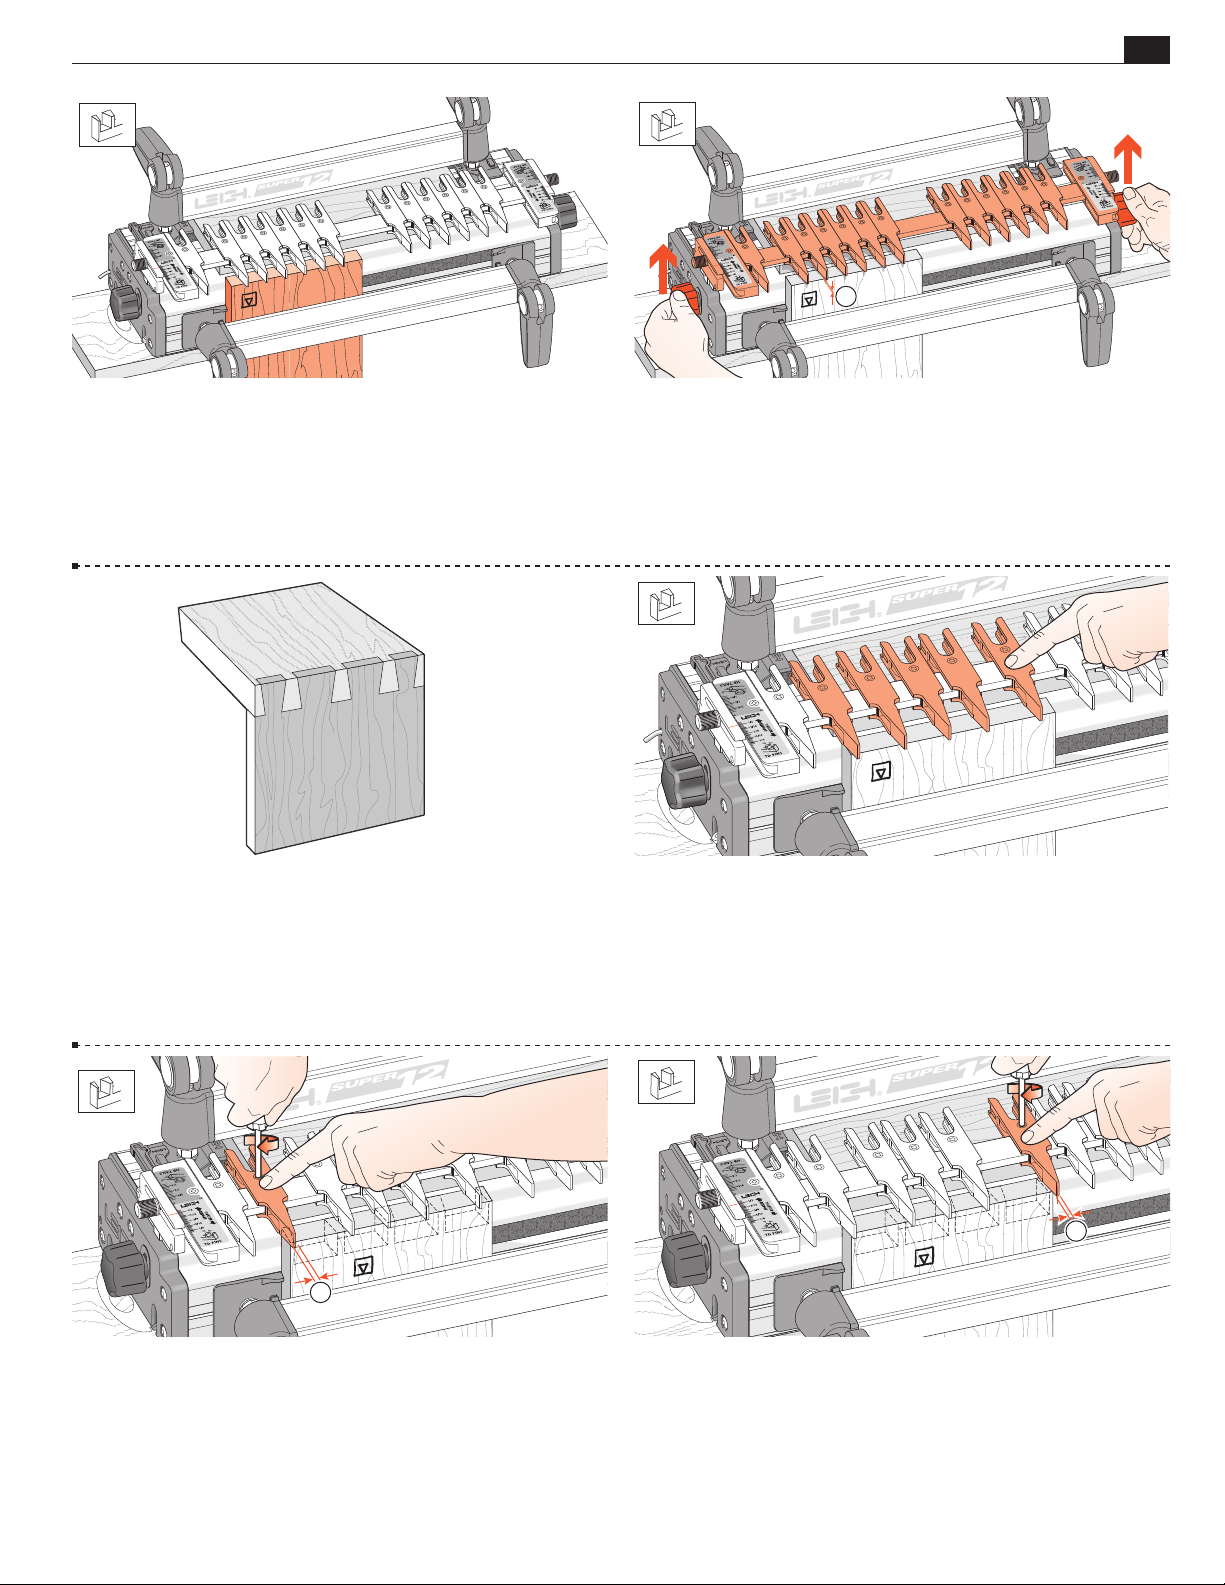
8-7 Clamp a tail board against the left front side stop, top edge
touching flush under the guidefingers, inside face i away from the
jig body. Although you will cut tails first, adjust the guidefinger
layout in
TD PINS mode. The adjustment screws are on top in
d
this mode, and it's easier to visualize the finished joint pattern.
8-9 This joint layout is just a suggestion for this trial. It has a
typical, traditional symmetrical pin layout, with half-pins at each
edge. The Superjig however, allows for infinite dovetail spacing.
Also, boards of different thicknesses can be joined to each other
as shown in this illustration. Before attempting an asymmetrical
joint layout, see chapter 12.
8-8 Loosen the support bracket knobs and raise the finger
assembly about 1⁄16"[2mm] above the boards, then re-tighten
the knobs. This will allow easy and accurate guidefinger adjustment.
8-10 Ignoring the extreme outer guidefinger next to the scale
(it just supports the router), loosen the next five guidefingers and
slide them over the top of the workpiece.
1
8-11 Lock the left-most guidefinger with its center-line about
1
⁄8"[3mm] in from the left edge of the board to form a half-pin.
2
8-12 Leave three guidefingers over the board. Lock the rightmost guidefinger with its center-line about 1⁄8"[3mm] in from
the right edge of the board to form the other half-pin. Judge this
distance by eye: it need not be exact. The sockets and pins will
align automatically.
Page 28
22
Chapter 8 Sup er Jig -12-18-24 User Guide
THROUGH DOVETAIL PROCEDURES
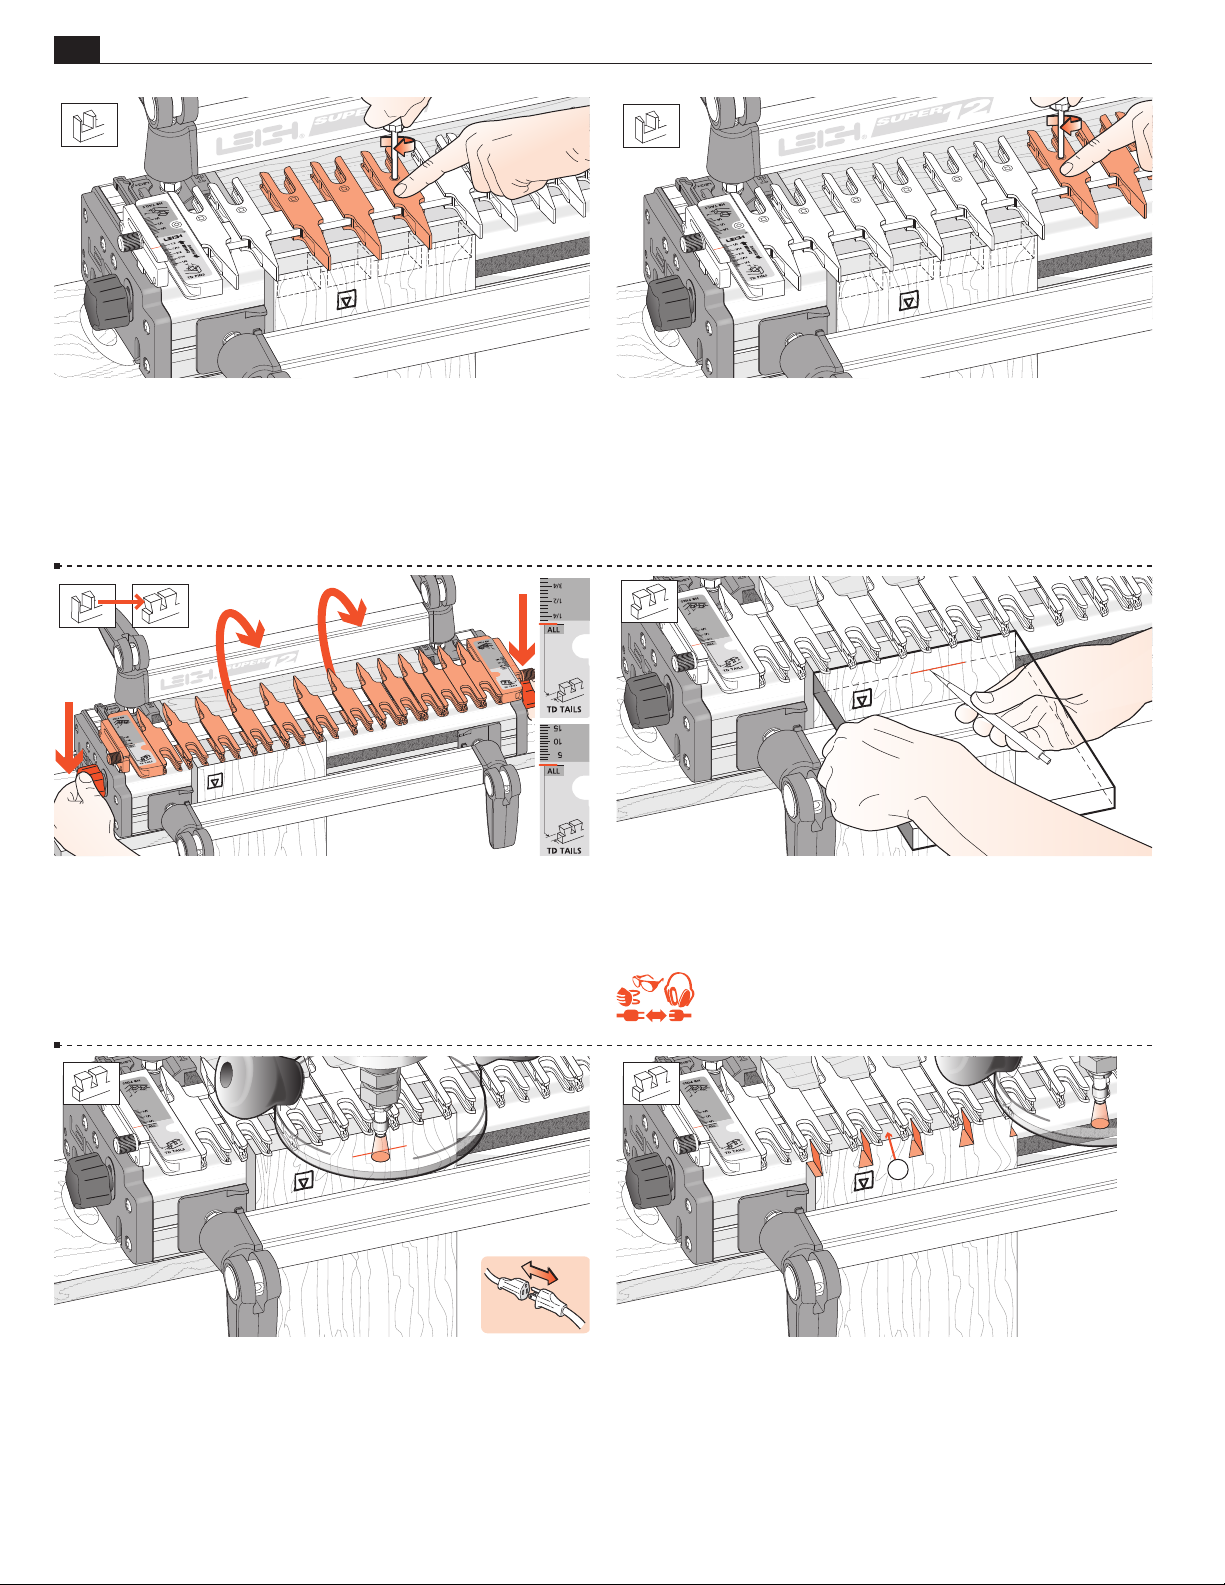
8-13 Space and lock the three remaining guidefingers as shown.
Again, judge it by eye. If it looks right on the jig, the finished joint will
look right.
8-15 Rotate the finger assembly to DTD TAILS mode, and set
it to the "ALL" position on the scale. Lower the finger assembly
onto the spacer board. All TD tails are routed at this "ALL"
setting. (This setting allows the dovetail bit to pass completely
through all tail boards.)
8-14 Tighten any other loose guidefingers.
8-16 Place the end of a pin board horizontally flush under the
guidefingers and mark a thin pencil line partly across the tail
board.
REMEMBER SAFETY!
8-17 Place the router on the finger assembly and adjust the router
until the dovetail bit tip is level with the center of the pencil line.
Note: This means the pin socket will be half a thin pencil line deeper
than the thickness of the pin board, leaving minimal clean-up after
assembly.
Check to make sure the bit rotates freely.
1
8-18 Plug in the router and rout out the half-pin and pin sockets.
Use only light side pressure on the guide fingers. Make sure to
run the guidebush along both sides of the finger opening. Take
care not to rout unwanted sockets where there are gaps between
pairs of fingers . Rout only between the rounded guidefinger
tips. See Hints and Tips Chapter 15.
Page 29
THROUGH DOVETAIL PROCEDURES
Chapter 8Sup er Jig -12-18-24 User Guide
23
8-19 Before removing the routed board from the jig, check by
eye and touch to make sure no parts have been missed. Release
the clamp and reverse the tail board in the jig, keeping the same
inside face
away from the jig body.
i
8-20 Rotate the finger assembly to dTD PINS mode and set
1
it on the
⁄2"[12,7mm] mark . Do not change the guidefinger
layout.
Rout the other end of this tail board and both ends of the second
tail board in the same fashion.
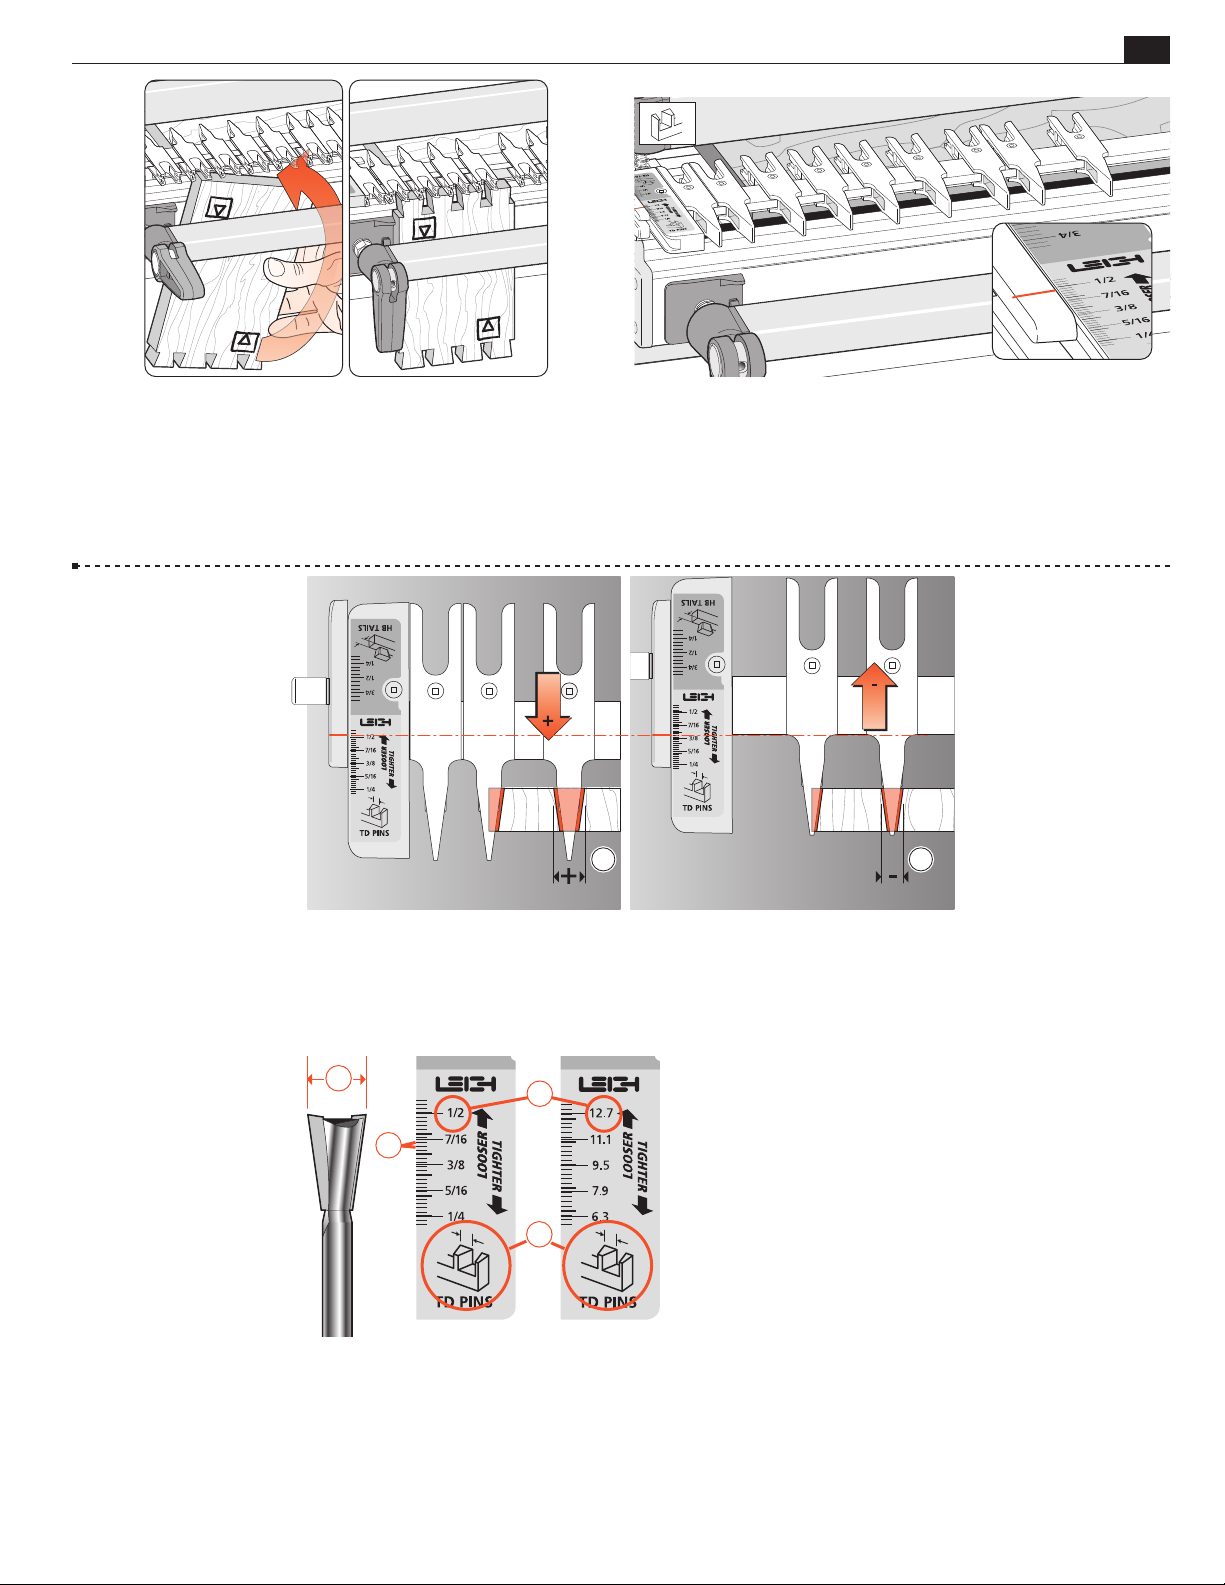
1 2
8-21 Finished Joint Tightness
The tightness of the finished joint is determined in dTD PINS mode. The farther out toward the operator the finger assembly is
set, the larger the pins will be . Moving the finger assembly in will make the pins smaller .
3
4
1
2
8-22 How the TD PIN Scales Work
The dimensions on the TD Pin scale indicate the major width of the pin to be routed . This matches the size of dovetail bit just
used to rout the tails . The increment lines on the scale are spaced so that moving the finger assembly by one increment changes
the joint glue-line gap by just 0.005"[0,125mm]. Even better, a one quarter division movement changes the fit by 0.00125"[0,03mm],
a tiny one and a quarter thousandth of an inch! Once you achieve the desired joint fit, simply record the setting using the illustrations
at the end of this chapter.
Page 30
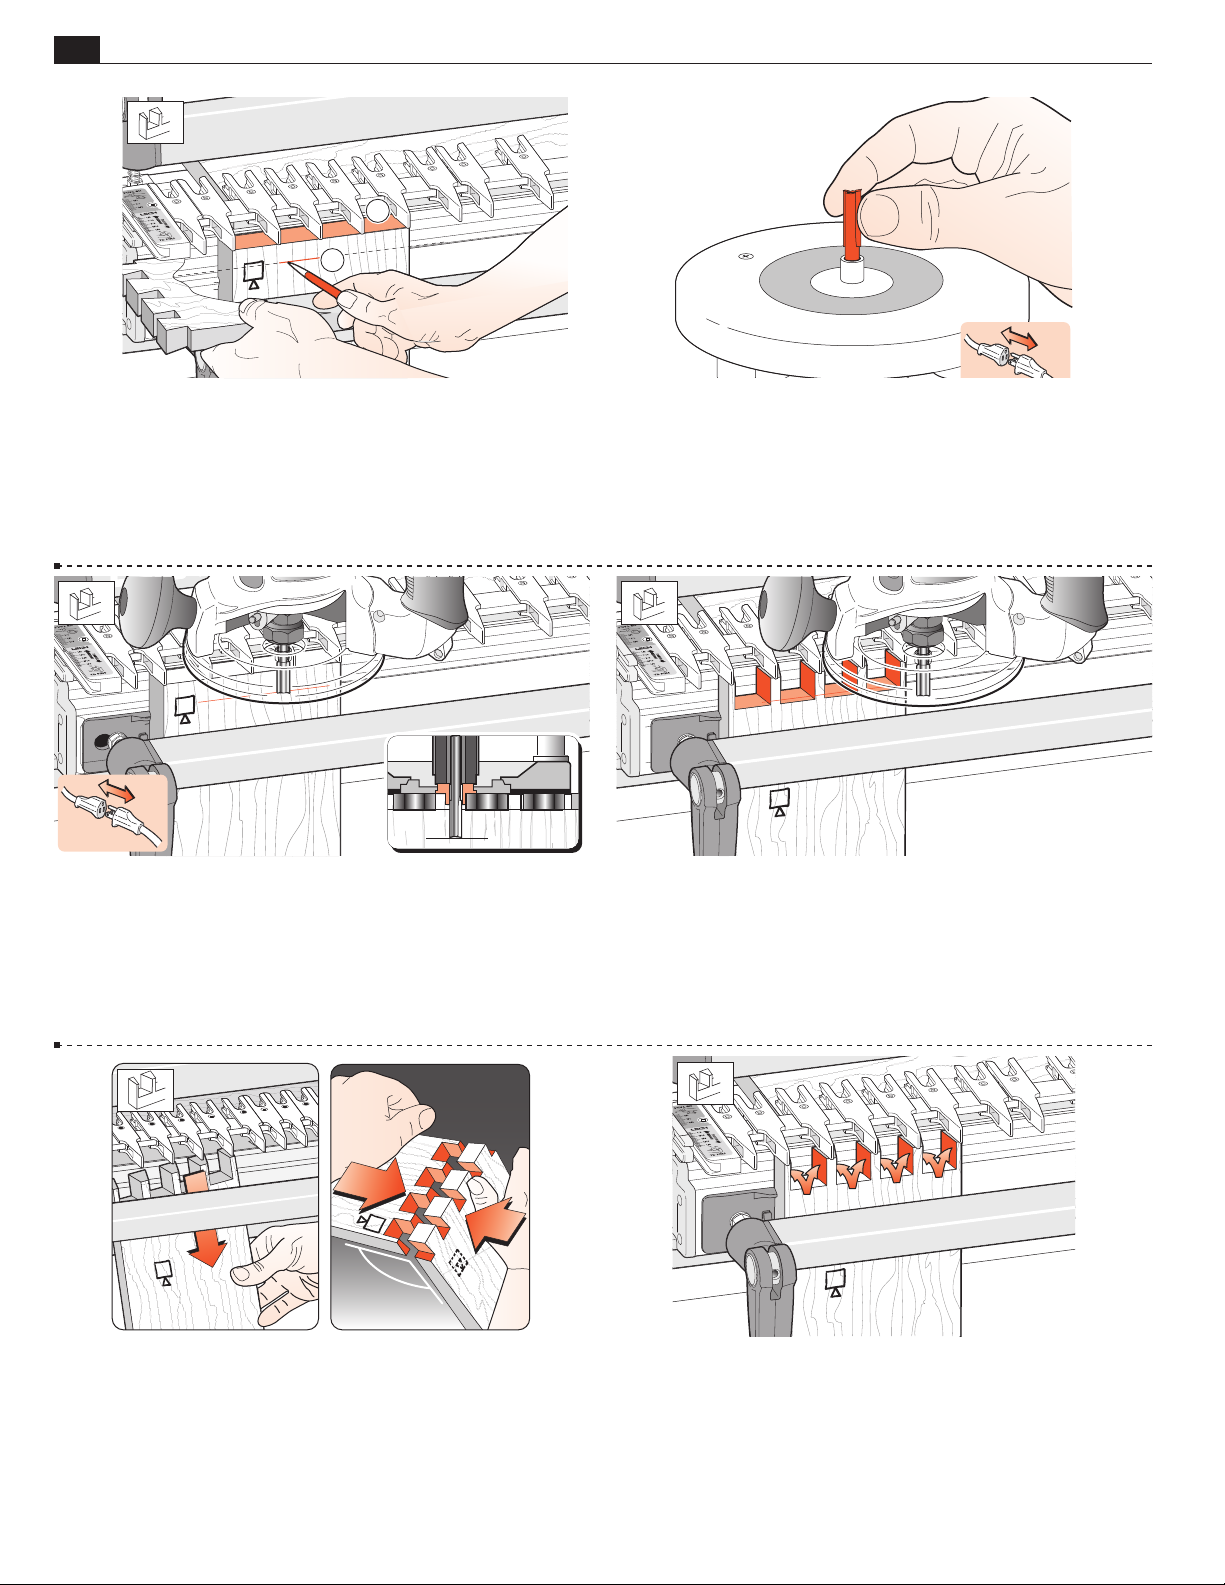
24
90
o
Chapter 8 Sup er Jig -12-18-24 User Guide
1
2
THROUGH DOVETAIL PROCEDURES
8-23 Clamp a test pin board against the left hand side stop,
outside face o away from the jig, with the top end flush under
the guides .
Place the side edge of one of the finished tail boards horizontally
flush under the guidefingers and mark a thin pencil line part way
across the pin board .
8-25 Place the router on the finger assembly and adjust the router
until the bit tip is level with the center of the pencil line. Check
to make sure the bit rotates freely.
Unplug the router and remove the dovetail bit. Mount the
8-24
included No. 140-8 straight bit to the router.
8-26 Rout out the waste between the pins. Check to make sure
no parts have been missed. See Chapter 15 "Hints and Tips" on
how to minimize tearout.
8-27 Remove the test pin board from the jig and test it for fit in
one of the tail boards.
Make sure the outside faces outward on both pieces. A firm push fit
is perfect, perhaps a tap with the heel of your hand. Having to use
a mallet means the joint is too tight to take glue.
8-28 If it is too tight, move the finger assembly in (away from
you) by one division on the scale. If it is only a little tight, adjust
the scale by only half a division. Replace the same pin board back
in the jig, carefully aligned against the same side stop. Rout off
the sides of the pins and test it again for fit. Repeat as necessary
to get a good fit.
Page 31
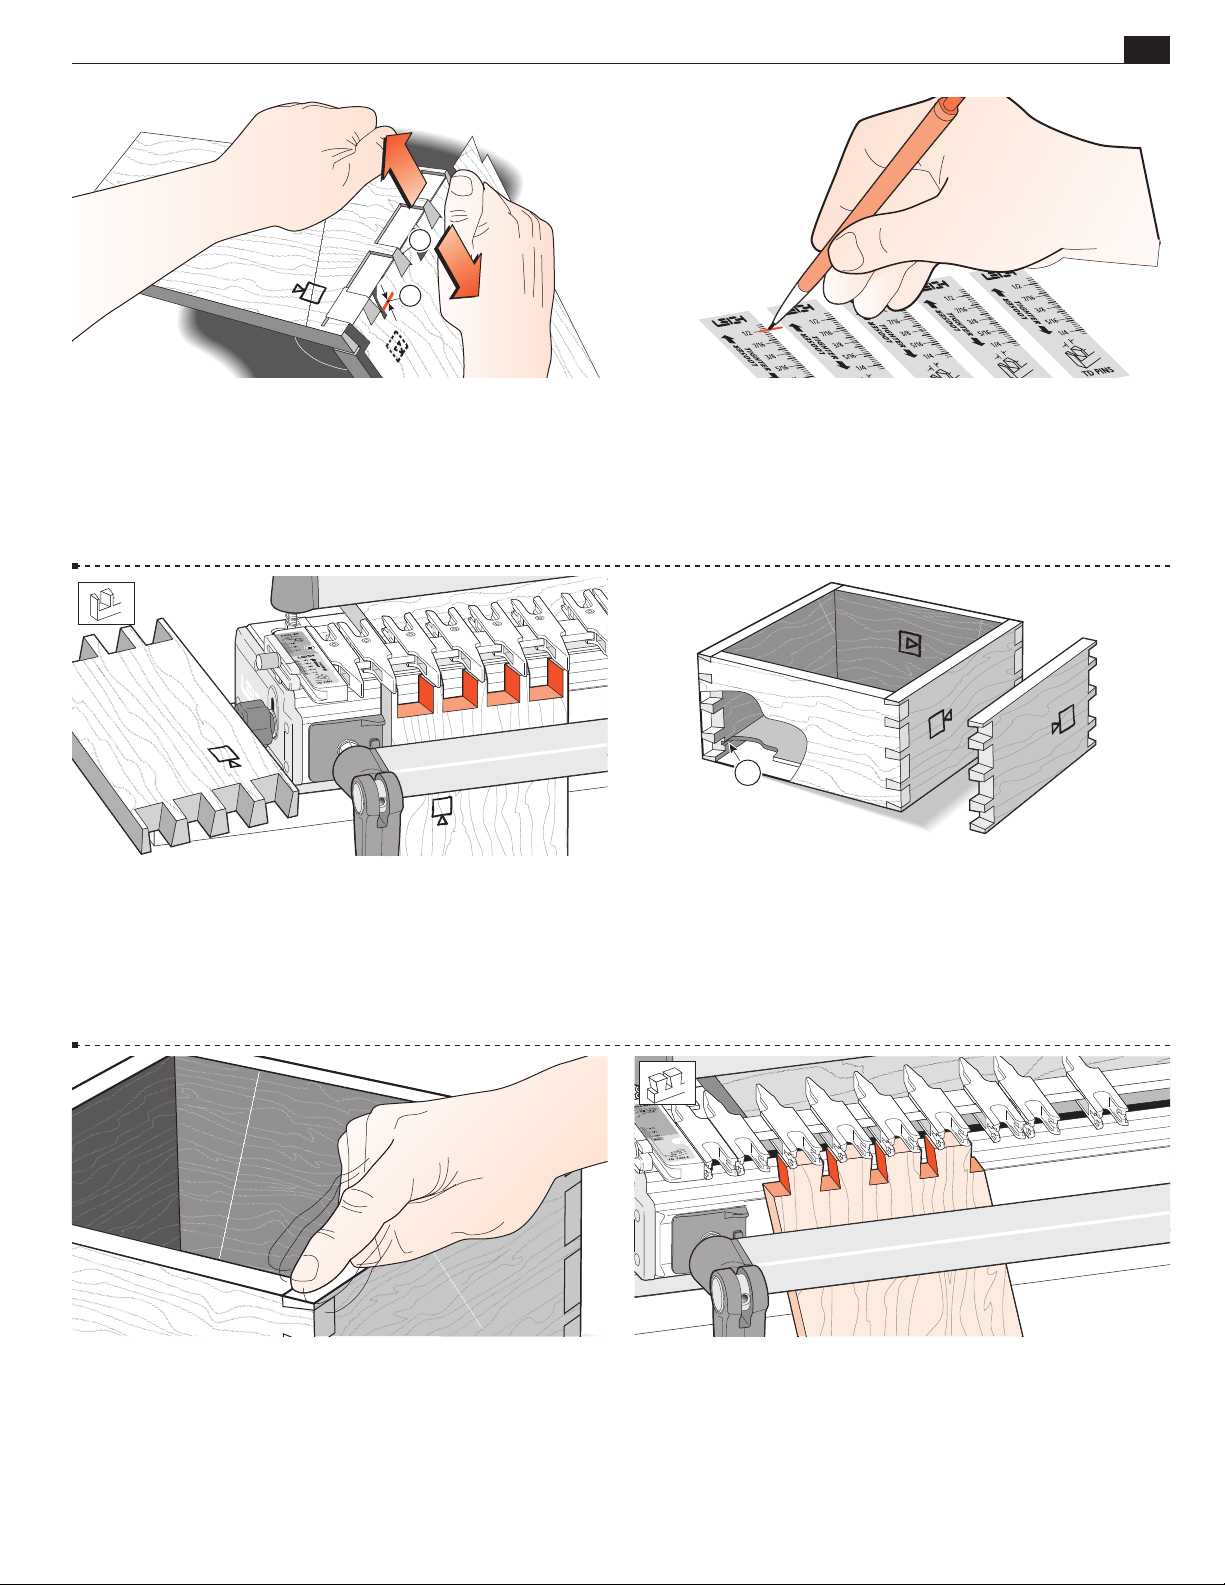
THROUGH DOVETAIL PROCEDURES
Chapter 8Sup er Jig -12-18-24 User Guide
1
2
o
90
25
8-29 If the joint is loose, pull the pin board so that the angled
sides of the pins and sockets jam tight together . The gap at the
bottom of the pins is the amount you will have to move the
finger assembly out (toward you). Reset the finger assembly and
test again on the other end of this board.
8-31 Rout all four ends of the pin boards, keeping the outside
face o outwards. (With luck you may not have used the fifth
board.)
Once the correct fit is achieved, mark the final dTD PINS
8-30
scale setting on the pull-out or on one of the scale prints at the
end of this chapter. Very slight variations to the scale setting may
be necessary with different wood species or hardness. You can also
note this on the Quick Reference pull-out card.
Y
A
1
X
Y
X
A
8-32 Assemble the box, making sure the tail boards face the
proper way, i.e. tail boards inside face in i; pin boards outside
face out
o. Provided you haven't already routed out the drawer
bottom grooves , it doesn't matter which edge of any of the
boards are at the top or bottom, the box will still fit together i.e.
pin board “A” can be up either way.
8-33 The box should be square and in plane. If it is not in plane
(i.e., the side edges of each board are not in line), then either the
ends of the boards are not square, the board widths are not exactly
equal, or there is a concentricity problem (see 7-2 to 7-7).
8-34 To form angled dovetails, refer to the Technical bulletin
“How to Rout Angled Through Dovetails on your Leigh Jig”. You
can download a printable file of the bulletin from our website:
www.leighjigs.com/support.php.
■
Page 32
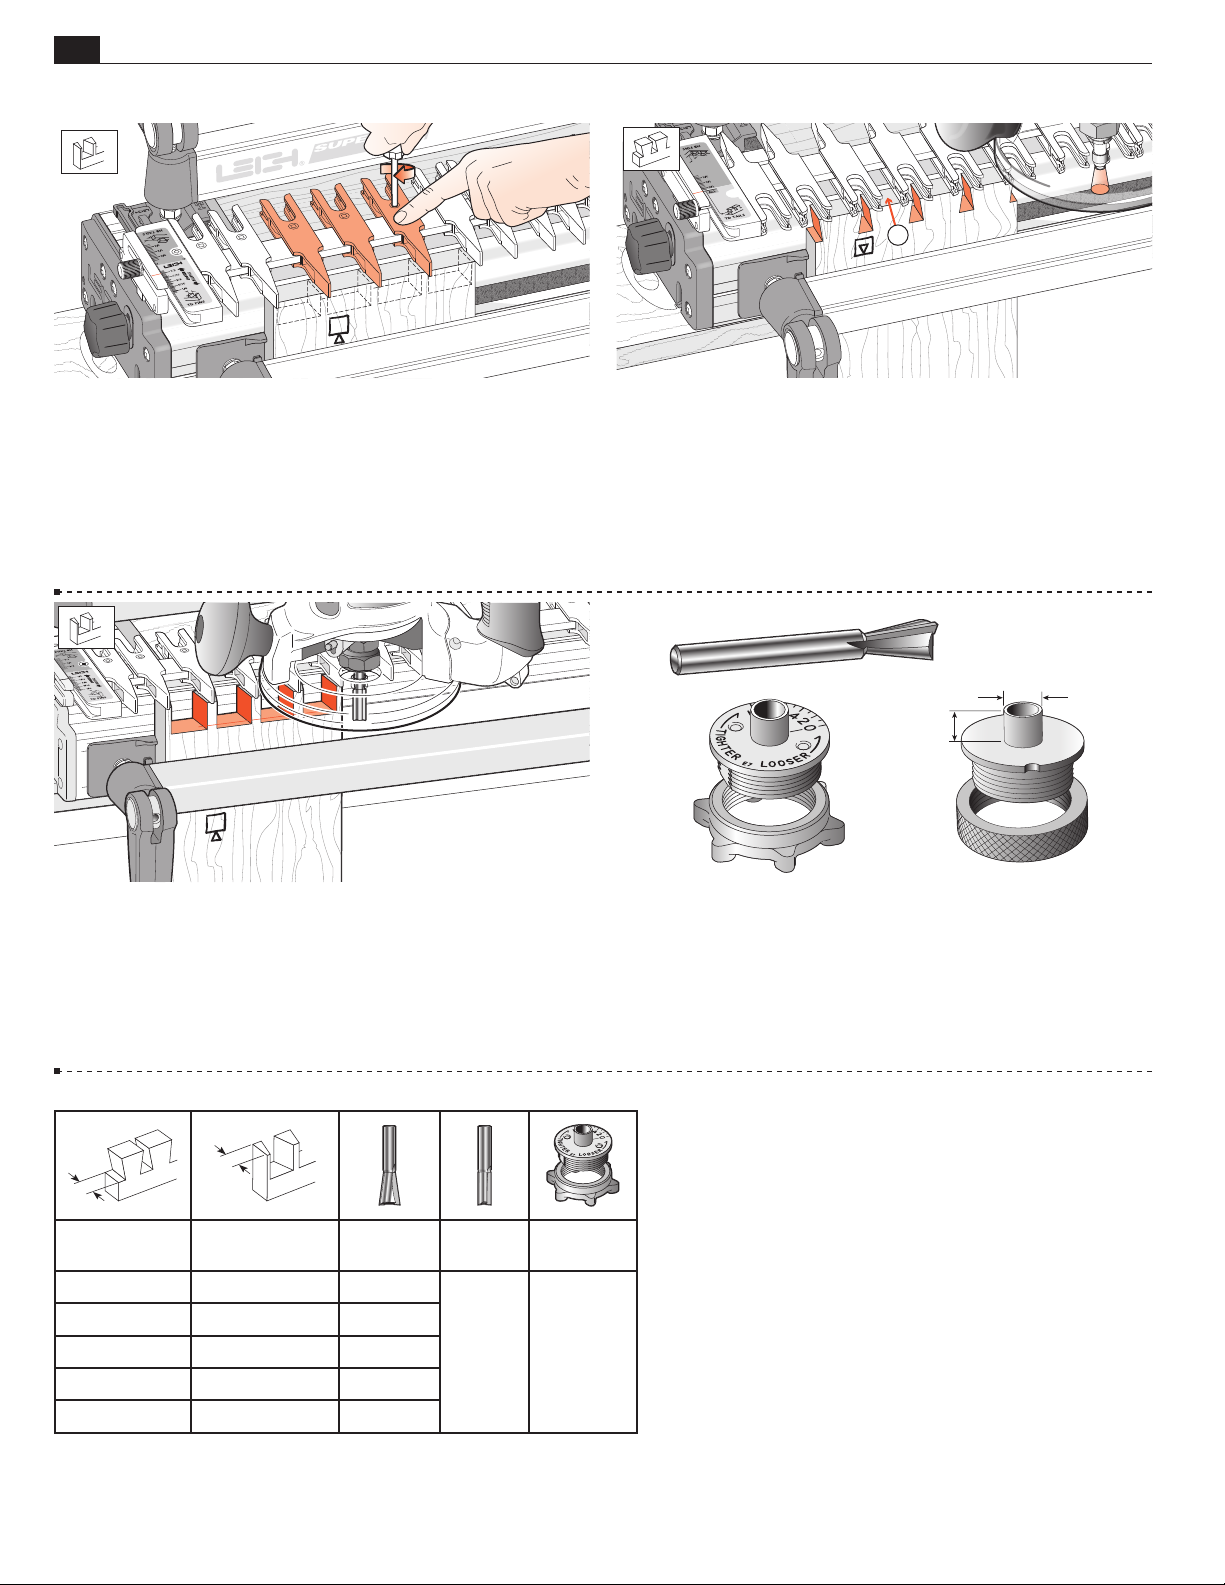
26
Chapter 8 Sup er Jig -12-18-24 User Guide
QUICK REFERENCE REMINDERS
THROUGH DOVETAIL PROCEDURES
1
8-QR1 Through dovetails are laid out in dTD PINS mode with
the finger assembly slightly raised above the spacer board and the
pin board. The outside face
of the TD pins is away from the
o
jig body.
8-QR3 The finger assembly is in dTD PINS mode, with the
scale set to a recorded setting (see detailed fit instructions, 8-24 to
8-30). TD pins are cut with a straight bit; the only time a straight
bit is used in dovetailing.
This is the only one of the four main modes that puts the outside
face of the board away from the jig body.
8-QR2
TD tail boards are clamped vertically in the jig. The
inside face i of the TD tails is away from the jig body. The finger assembly is in
TD TAILS mode, set on the “ALL” setting.
D
There is only one setting in this mode.
7
16
"
[11,1mm]~
/
1
4
"
/
[6,35mm]
8-QR4 Through dovetail tails are always routed with an 8° dovetail
bit to match the 8° guide finger. All through dovetail routing on the
Superjig is done with the Leigh e7-Bush, or any ~7⁄16" [11,1mm]
1
diameter bush (min. barrel length
/4"[6,35mm]). See page 68 for
more on routers and guide bushings.
Thickness of
Tail Board
13
/16"[21]1/2" - 13/16" [12-20] No.80-8
up to
13
up to
/16"[21]3/8" - 5/8" [10-16] No.75-8
13
/16"[21]1/4" - 1/2" [6-13] No.70-8
up to
13
/16"[21] up to 3/8" [10] No.60-8
up to
13
/16"[21] up to 1/4" [6] No.50-8
up to
Numbers in brackets are millimeters
Thickness of
Pin Board
Dovetail
Bit
Straight
Bit
No.140-8
Guidebush
Diameter
e7-Bush or
~7
/16" [11,1]
diameter
bush
8-QR
5
Here is a quick reference selection chart for through dovetail
bits and guidebushes. Please study the bit and guidebush
13
■
⁄16"[20mm]
selection appendices for a full explanation. Note:
is the maximum through pin board thickness.
Page 33
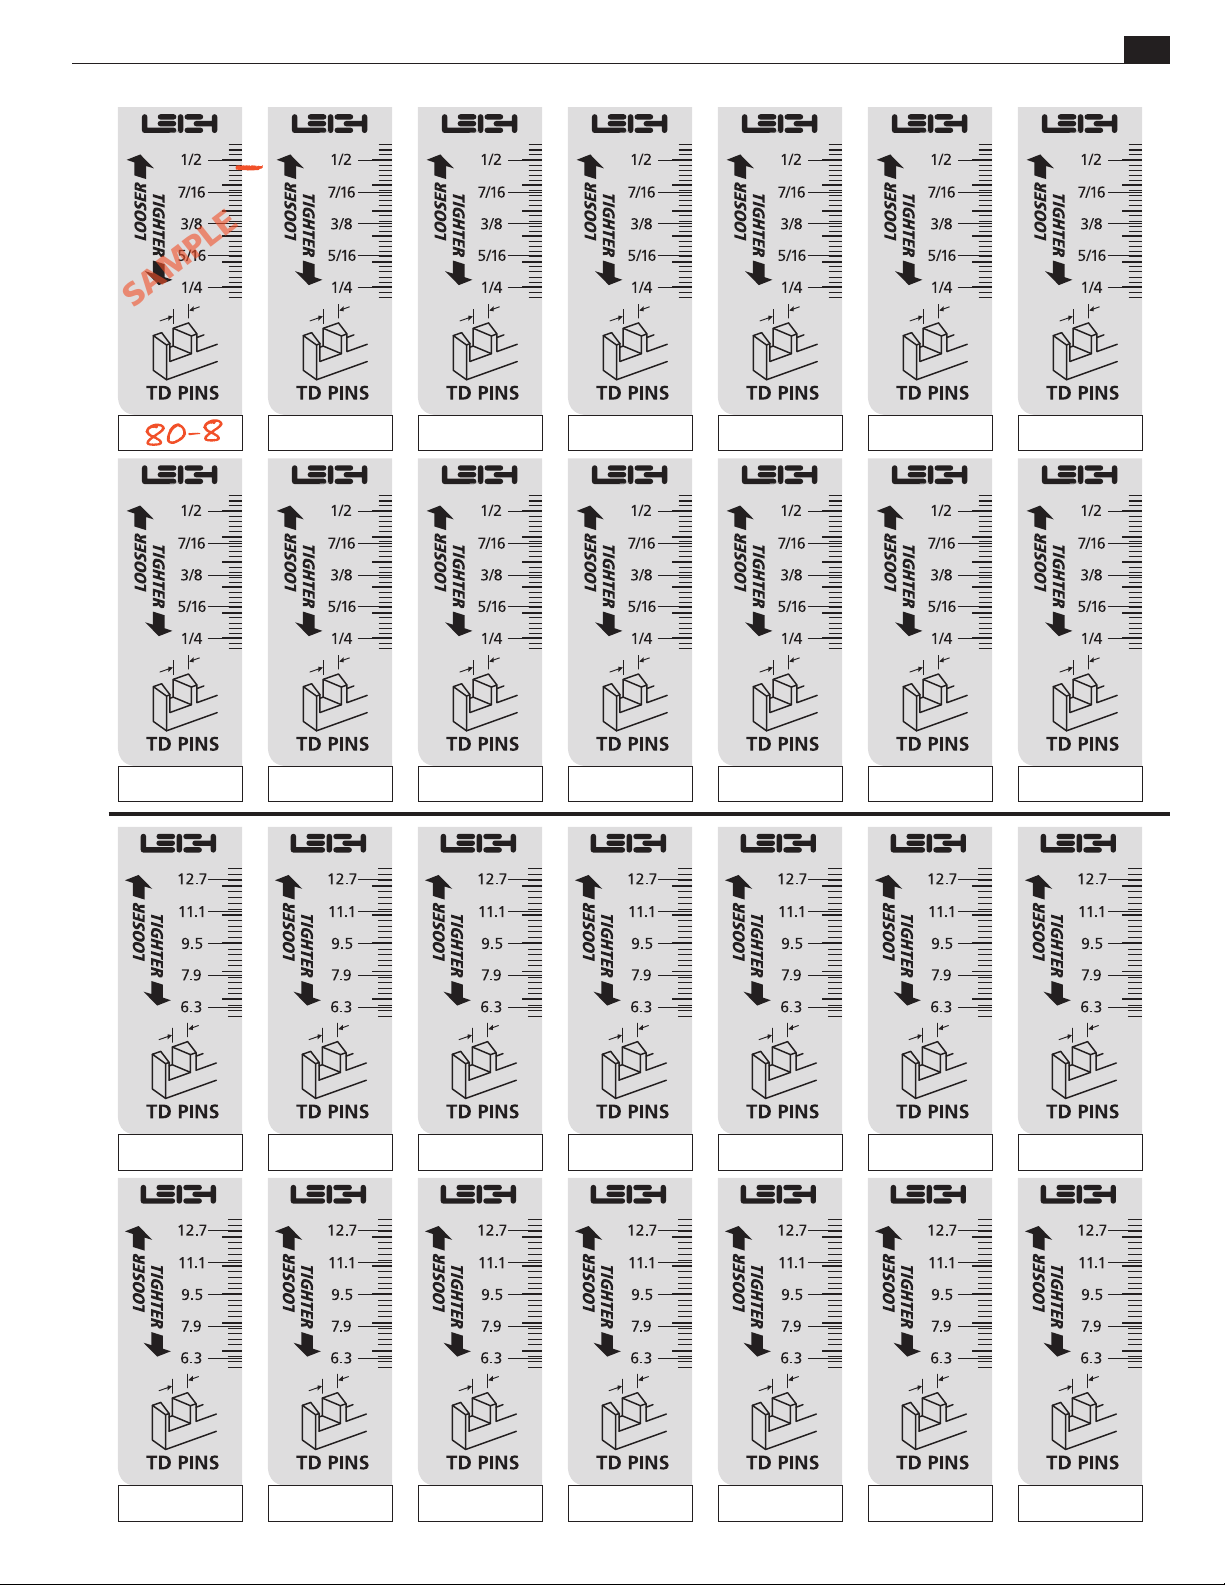
THROUGH DOVETAIL PROCEDURES
SAMPLE
INCHESMETRIC
Project Settings
Chapter 8Sup er Jig -12-18-24 User Guide
27
Page 34
28
Chapter 8 Sup er Jig -12-18-24 User Guide
THROUGH DOVETAIL PROCEDURES
Page 35
SUPERJIG - CHAPTER 9
Variably Spaced Half-Blind
Dovetail Procedures
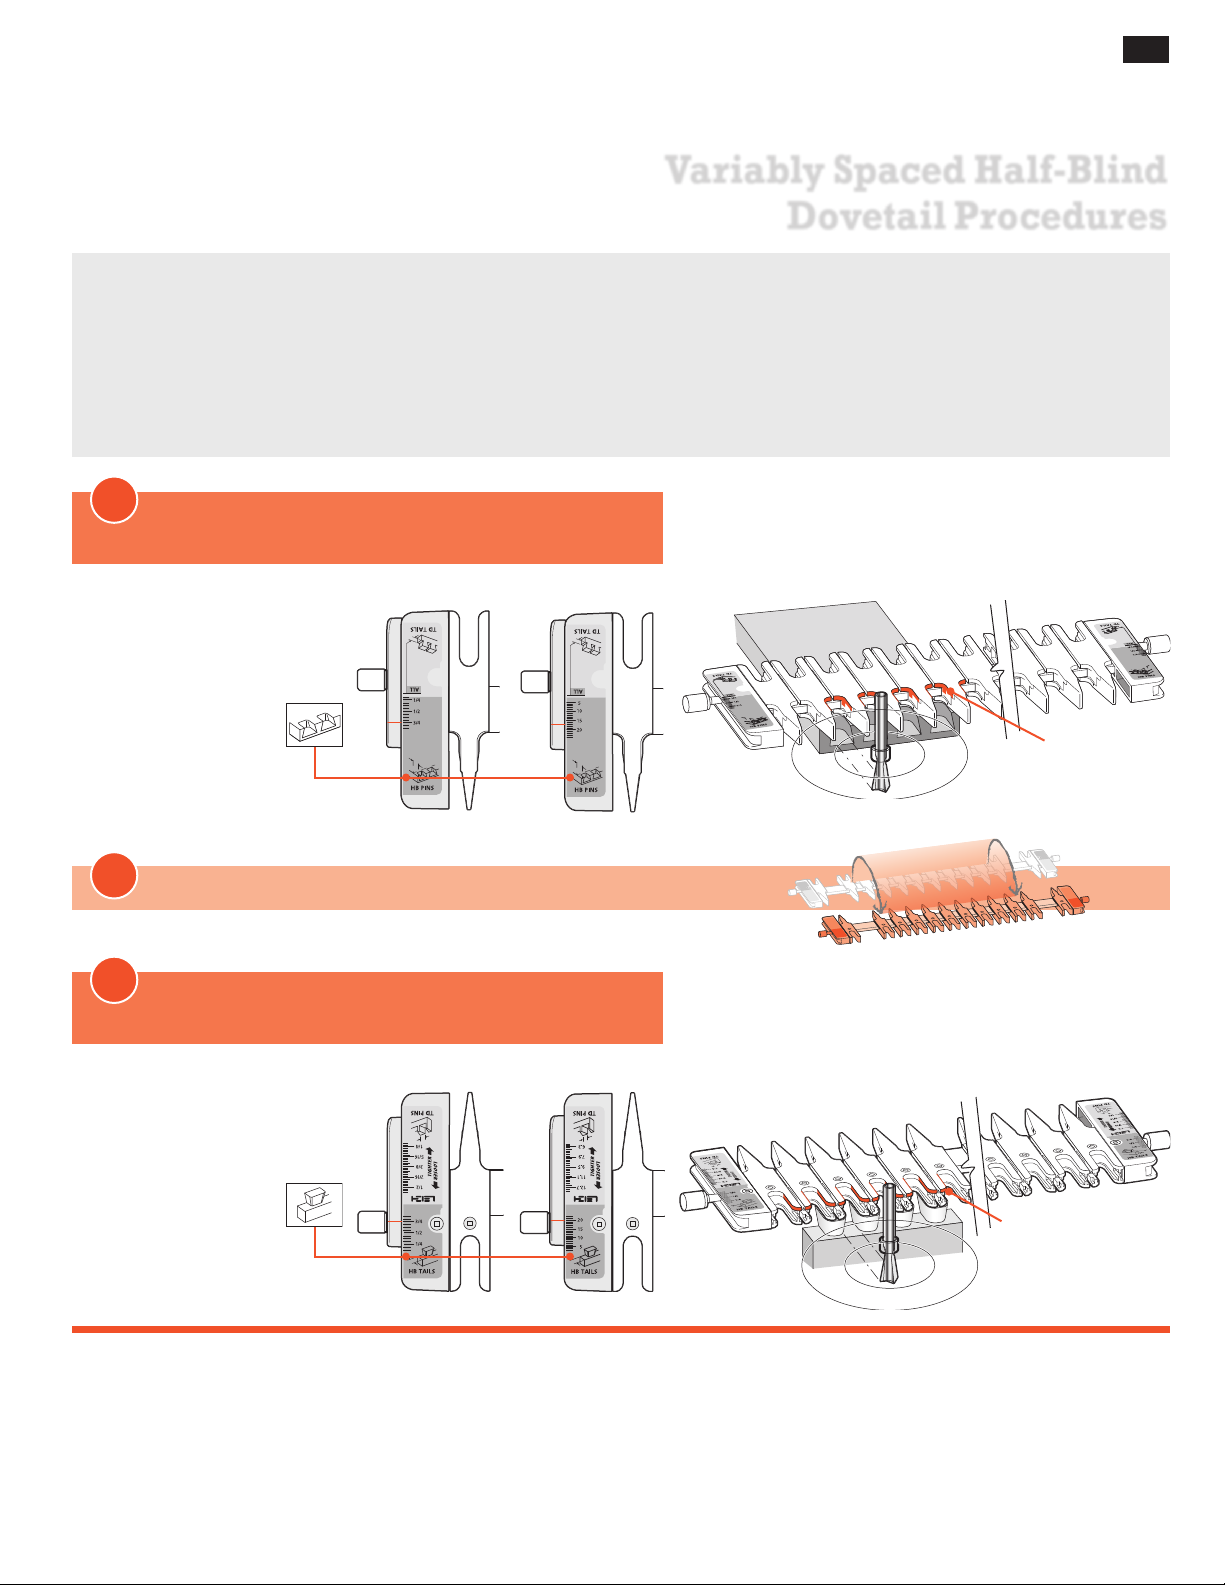
IMPORTANT! The most commonly misunderstood aspect of routing half-blind dovetails is how the dovetail bit’s
depth of cut is used to adjust the joint fit, and how the angle of the bit affects that depth of cut. Review this chapter
for a clear understanding of this concept.
Note: Use the e7-Bush set at “10”, or any round ~7/16"[~11,1mm] bush (min. depth 1/4" see page 67), and any
one of the five bits listed on the next page may be used for half-blind dovetails. See Appendix II “Half Blind Bit
Selection” for a full description on how to select an appropriate bit.
1
Start in
Half-Blind Dovetail Pins (HB PINS) mode
29
MODE ICONS
Illustrations in this user
guide include the correct
mode icon for the current instruction. The
icons are also used in
the instruction text.
2
ROTATE the finger assembly toward you 180°
3
Now the Finger Assembly is in
Inches
Half-Blind Dovetail Tails (HB TAILS) mode
Inches
Millimeters
Active
Guide Surfaces
HB PINS
HB TAILS
Millimeters
Active
Guide Surfaces
Page 36
30
" [3,2mm] Min.
Board Thickness
" [3,2mm] Min.
Board Thickness
Chapter 9 Sup er Jig -12-18-24 User Guide
6
3
Depth
8
of Cut
1
22
5
4
Depth
7
of Cut
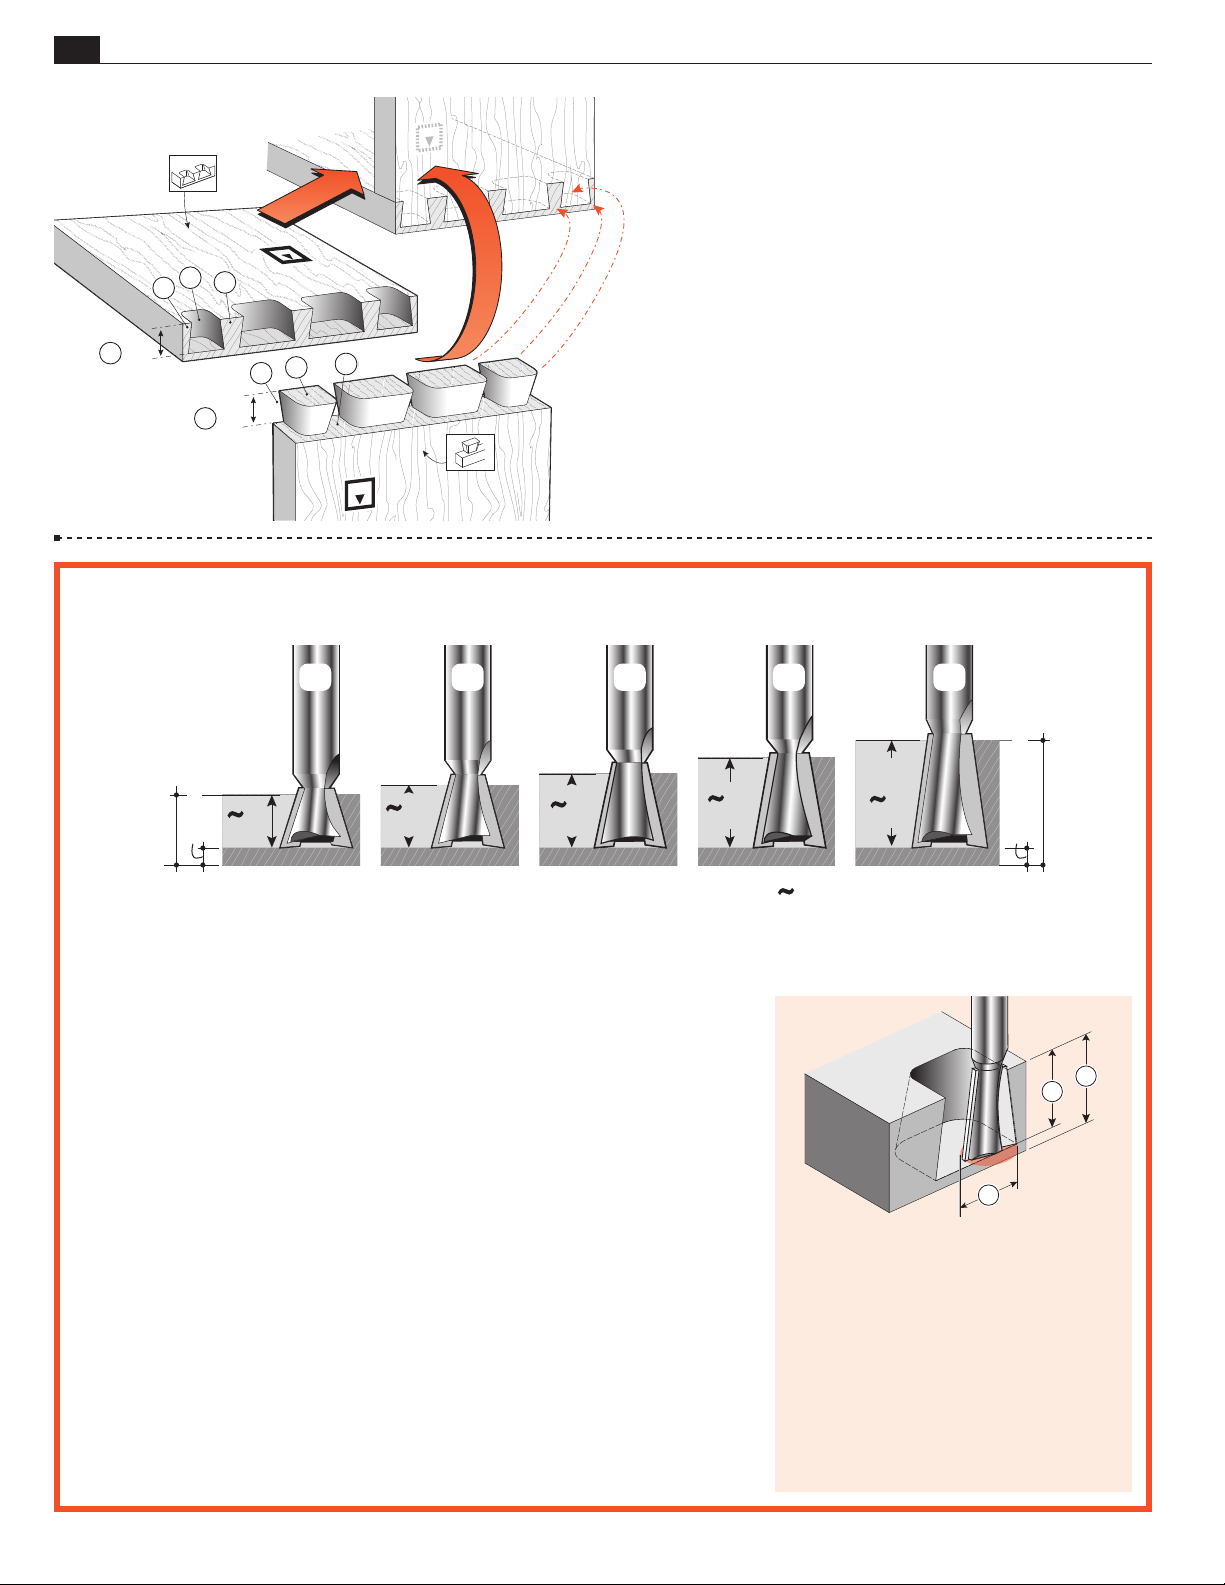
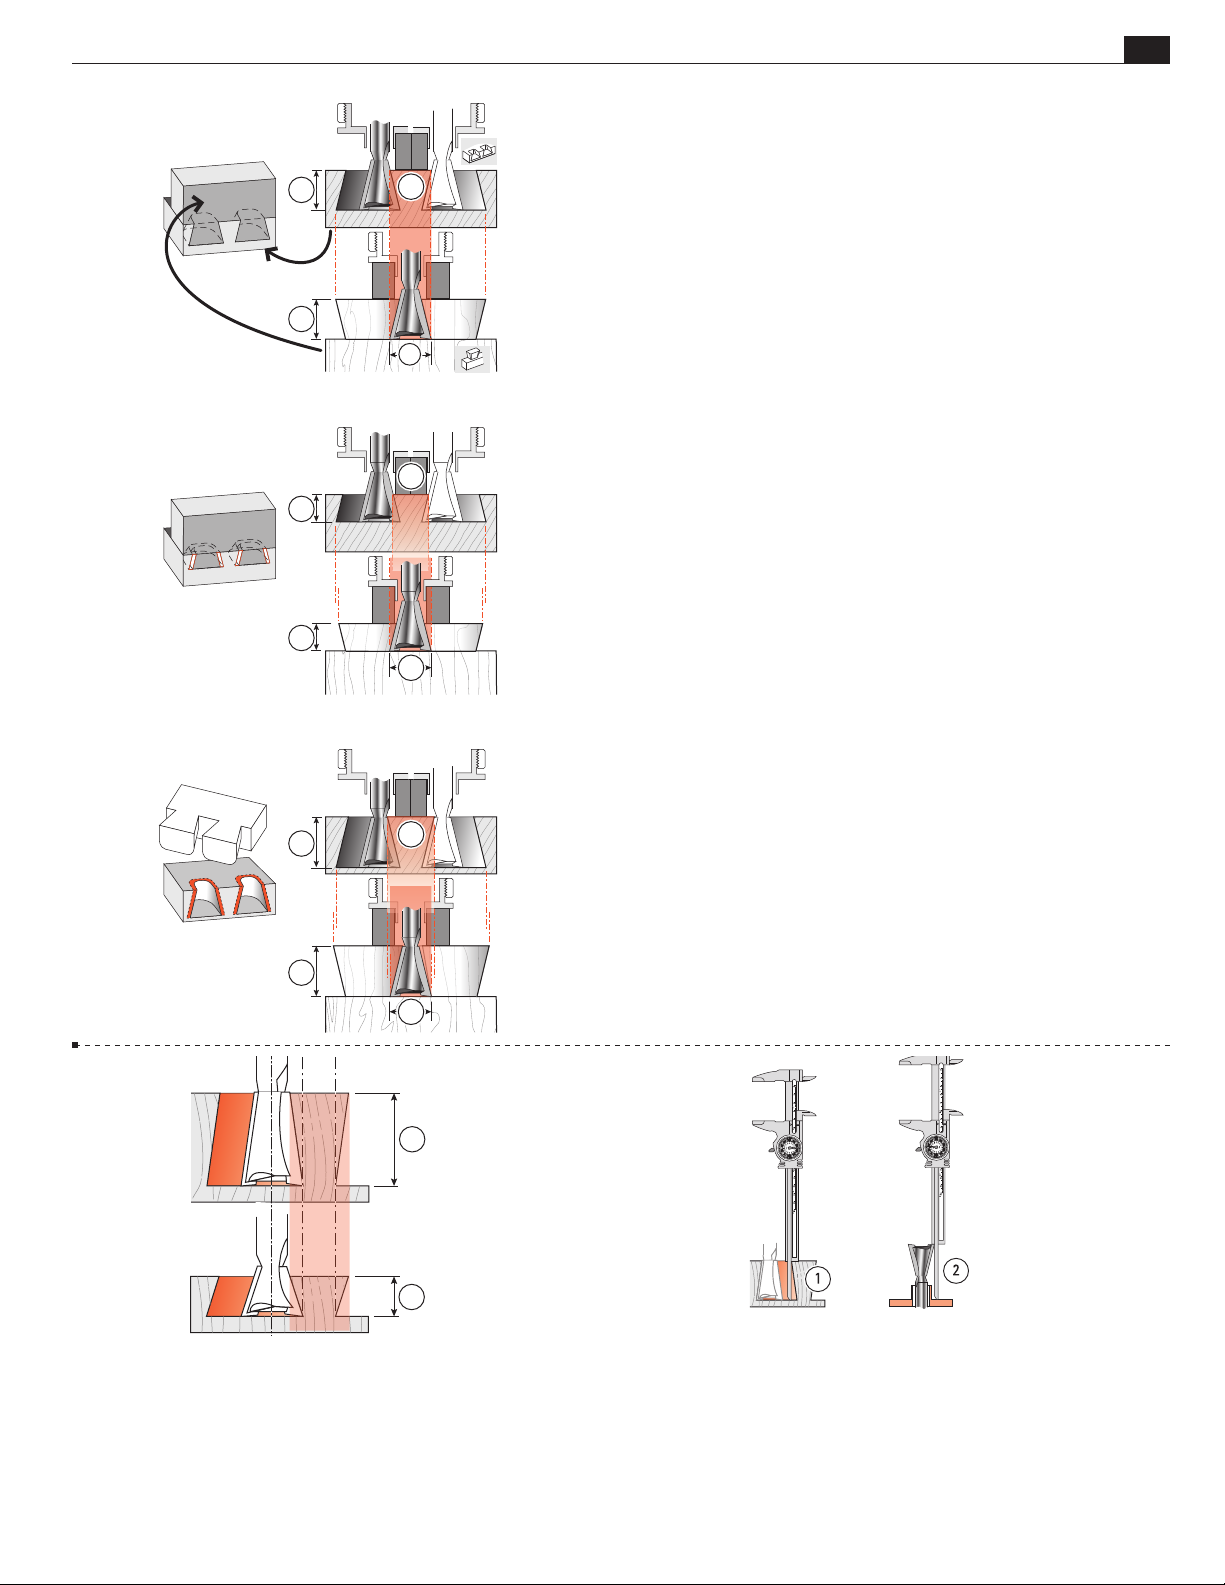
9-2 Cutting Depth for Variably Spaced Half-Blind Dovetails
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
9-1 Half-Blind Dovetail Terminology:
Pins
h
Pin sockets
Half-pins
Half-pin sockets
Tails
➆
➇
H
Tail sockets
Depth of Cut (tails)
Depth of Cut (pins)
The pins fit in the pin sockets. Joints almost always begin and
end with a half-pin as shown.
128-8
DEPTH
OF CUT
3
/8"
8
/
[9mm]
1
Note: Add at least
18
˚
[11mm]
1
⁄8"[3,2mm] to the depth of cut for board thickness.
Important! Read This About HB Depth of Cut
Bit selection is critical. You need to
select a specific dovetail bit for your
half-blind dovetail project, depending
on the pinboard (drawer front) thickness you are using.
• Choose one of the five 1⁄2" [12,7mm]
diameter dovetail bits shown above.
Check bit selection in Appendix II.
• Depth of cut must be as specified
for each of the five bits illustrated
above. Note: Leigh bits 101-8, 112-8
and 128-8 are optional.
• Raising the bit above its specified
cutting depth will result in loose
joints and may damage the jig, bit
and/or guidebush. A lower setting
7
/16"
120-8
14
[13mm]
˚
112-8
1
/2"
12
˚
will result in tighter joints that may
not fit together.
• Small Depth of Cut adjustments
will change joint fit tightness. See
why in Steps 9-3 to 9-5.
• Half-blind PINS and TAILS are
routed with the same dovetail bit
and must be at the same Depth of
Cut.
• All half-blind dovetail bits work
with the Leigh e7-Bush supplied
with your Leigh jig or standard
7
⁄16"[11,1mm] outside diameter
~
guidebush.
5
[16mm]
/8"
101-8
DEPTH
OF CUT
[19mm]
10
˚
Symbol for “approximately”
80-8
3
/4"
8
˚
3
PINBOARD THICKNESS
the
maximum depth of cut
use. Select a bit with a specified cutting
depth that is at least 1⁄8"
pinboard thickness.
A dovetail bit will produce
cific cutting depth.
Only
1⁄2" [12,7mm] cutting diameter
bits can be used for half-blind dovetails.
8
/
1
1
2
determines
you can
less
than the
only one spe-
Page 37
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
Chapter 9Sup er Jig -12-18-24 User Guide
31
PIN
1
3
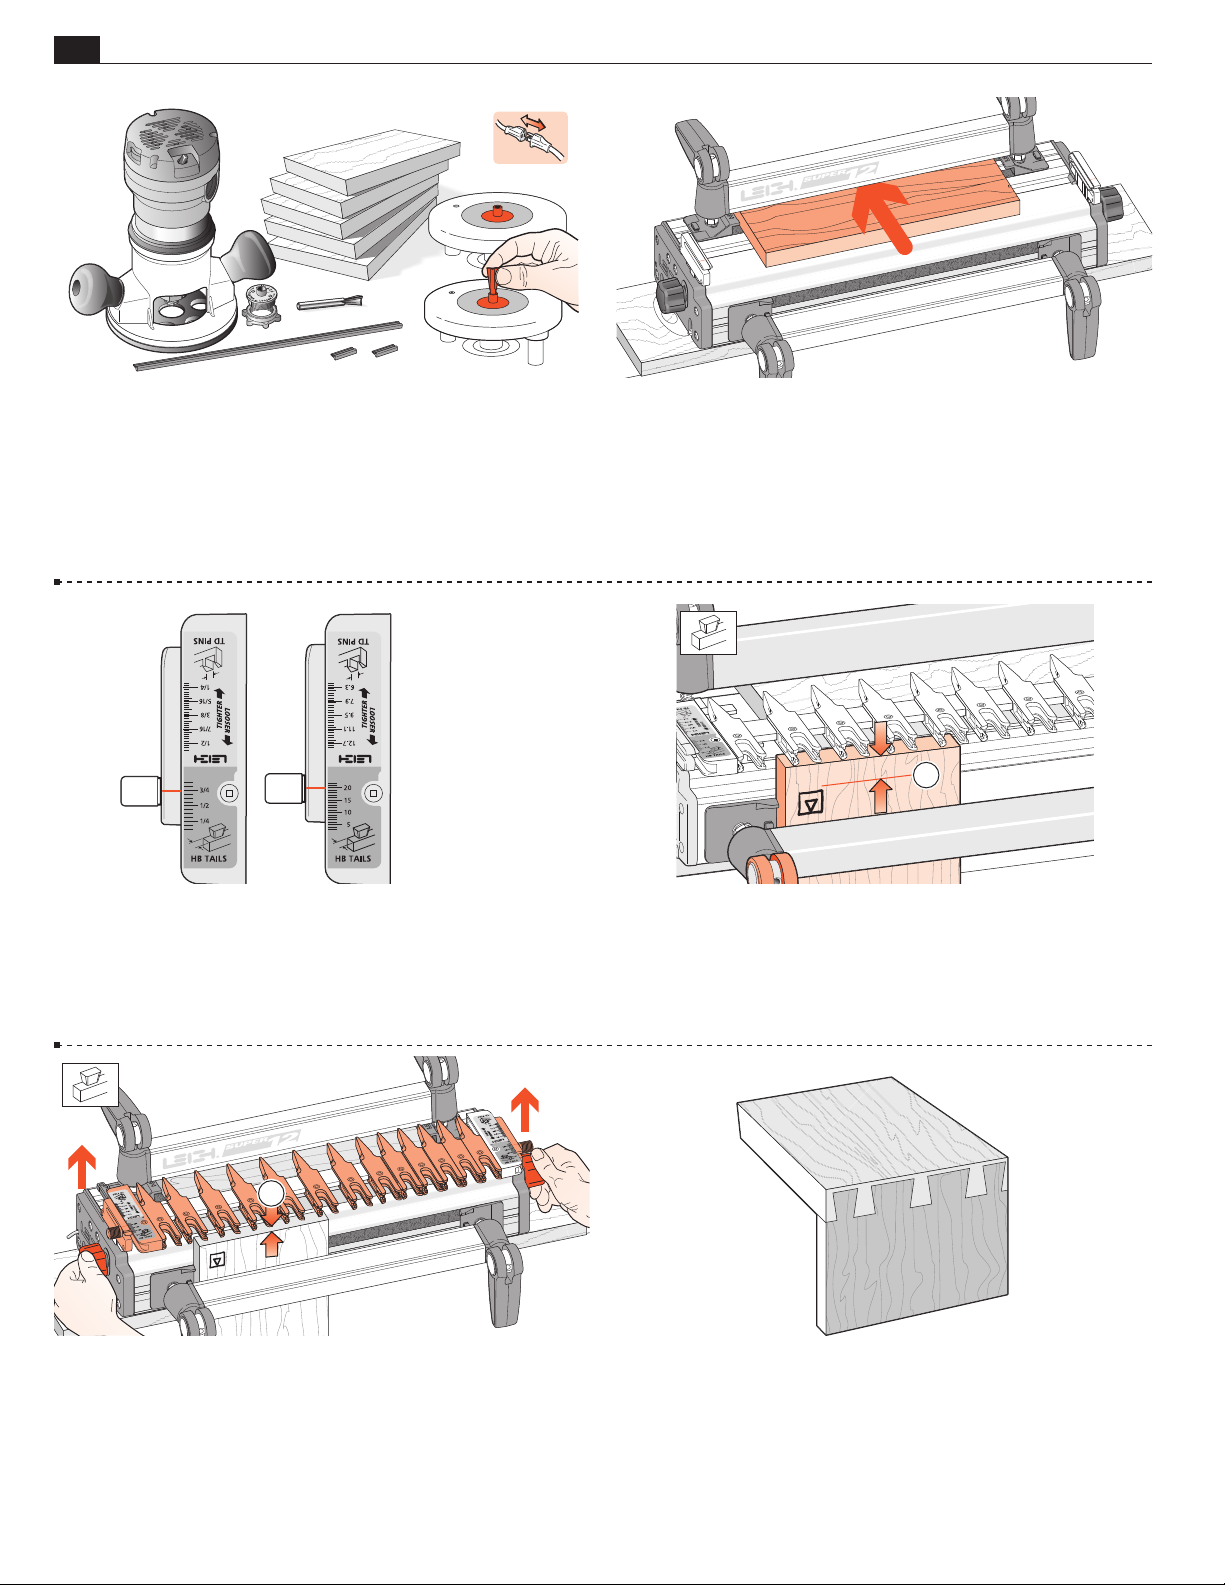
9-3 Joint Fit and Depth of Cut
Here’s why the depth of cut changes the fit in half-blind dovetails. Increasing or decreasing the depth of cut does not affect the
pin socket width , but does affect the width of the pin that
goes into the socket .
1
2
3
1
9-4 Note that decreasing the bit depth makes the pin
narrower while the pin socket stays the same width, producing
a loose fit.
Decreasing the bit depth (i.e. raise the bit into the router) produces a looser fit.
1
2
1
1
8˚
18˚
3
2
1
2
9-6 Bit Angle and Depth of Cut Half-blind pins and tails
are routed with the same dovetail bit, the same guidebush, and
the same depth of cut. A different depth of cut requires a different angled bit. Leigh offers five different angled dovetail bits for
a range of cut depths. A lesser angle, say 8˚, for a deeper cut ; a
greater angle, say 18˚, for a shallower cut .
Increasing the bit depth makes the pin larger while the
9-5
pin socket stays the same width, producing too tight a fit.
Increasing the bit depth (i.e. lower the bit) produces a tighter
fit.
9-7 Cumulative plus/minus tolerances in routers, bits and
guidebushes, make it impossible to state exact bit depth for firsttime precision fit. All dovetail jigs require trial and error tests to
attain fine fitting joints. The good news; we give a starting depth
for each bit. Test and measure the successful ‘Best fit’ depth of
cut or bit projection . Record for future first-time fits.
Page 38
32
Chapter 9 Sup er Jig -12-18-24 User Guide
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
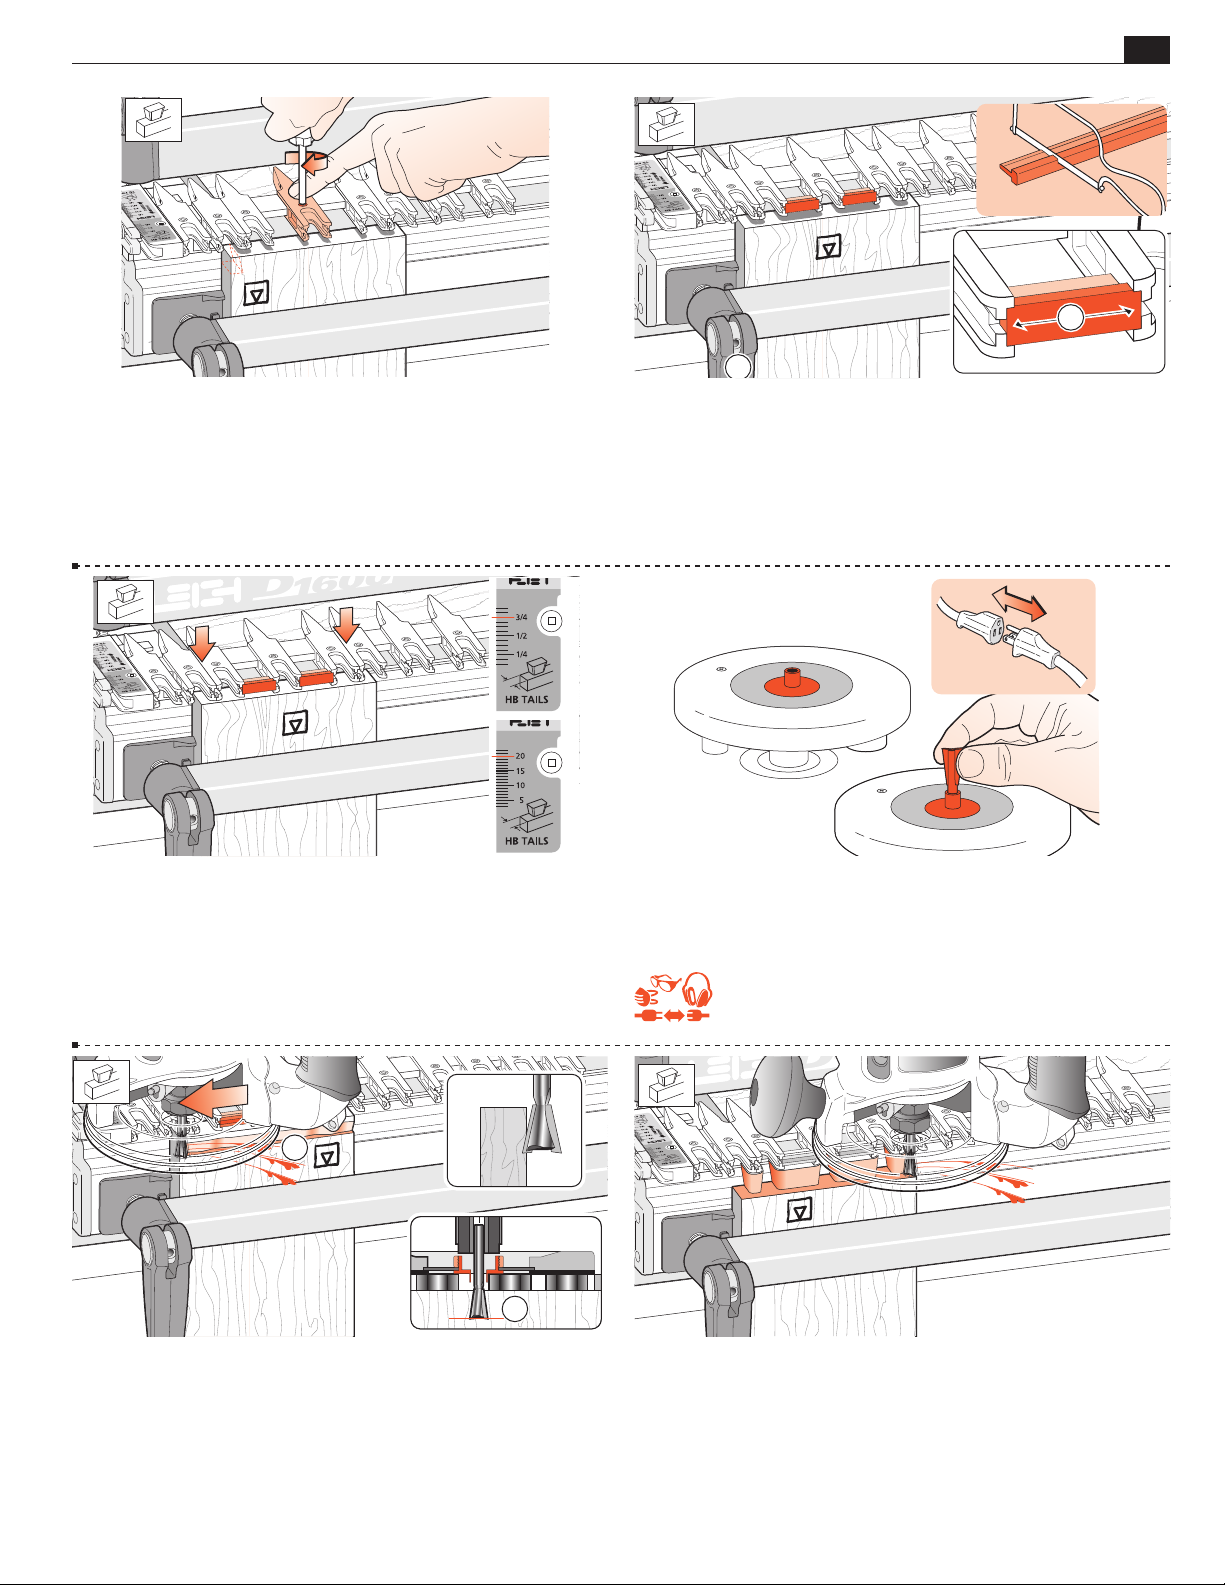
9-8 Routing a Test Joint Use the e7-Bush or a 7⁄16"[11,1mm]
1
diameter bush (min. depth
1
⁄2"[12,7mm] 14° dovetail bit. (80-series bits cut too deep for
3
⁄4"[20mm] boards, see HB bits, Appendix II). Select several pieces
3
⁄4"x5 1⁄2"[20x140mm] x about 8"[200mm], and the plastic
of
⁄4" see page 67) and No.120-8
bridge. Note: Half-blind pin boards must be minimum ½"[13mm]
thick to clamp. Thinner boards; see 9-21.
9-10 Mount the finger assembly on the support brackets in the
HB TAILS mode, flat on the spacer board, scales set on the
H
thickness of the tail board (
The
HB TAILS scale is always set at the tail board thick-
H
3
⁄4"[20mm] in this instance).
ness.
9-9 Clamp the spacer board in the rear clamp.
1
9-11 Measure and mark a line on the inside face of the tail board
to the bit’s depth of cut as in 9-2. Clamp this test tail board in
the left front clamp, against the side stop with the top edge flush
under the guidefingers, and the inside face i of the drawer side
away from the jig.
1
9-12 Unlock and raise the finger assembly support brackets
1
slightly so that the finger assembly is about
⁄16"[2mm] above
the boards. This will allow easy movement of the guidefingers.
9-13 The following joint design is suggested for this trial. It has a
typical and traditional even layout of pins, with half-pins at each
edge. The Leigh jig, however, allows for an infinite variety of joint
designs, and boards of different thicknesses can be joined to each
other as shown in this illustration. Before attempting joints of
asymmetrical design, see chapter 12.
Page 39
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
Chapter 9Sup er Jig -12-18-24 User Guide
2
1
33
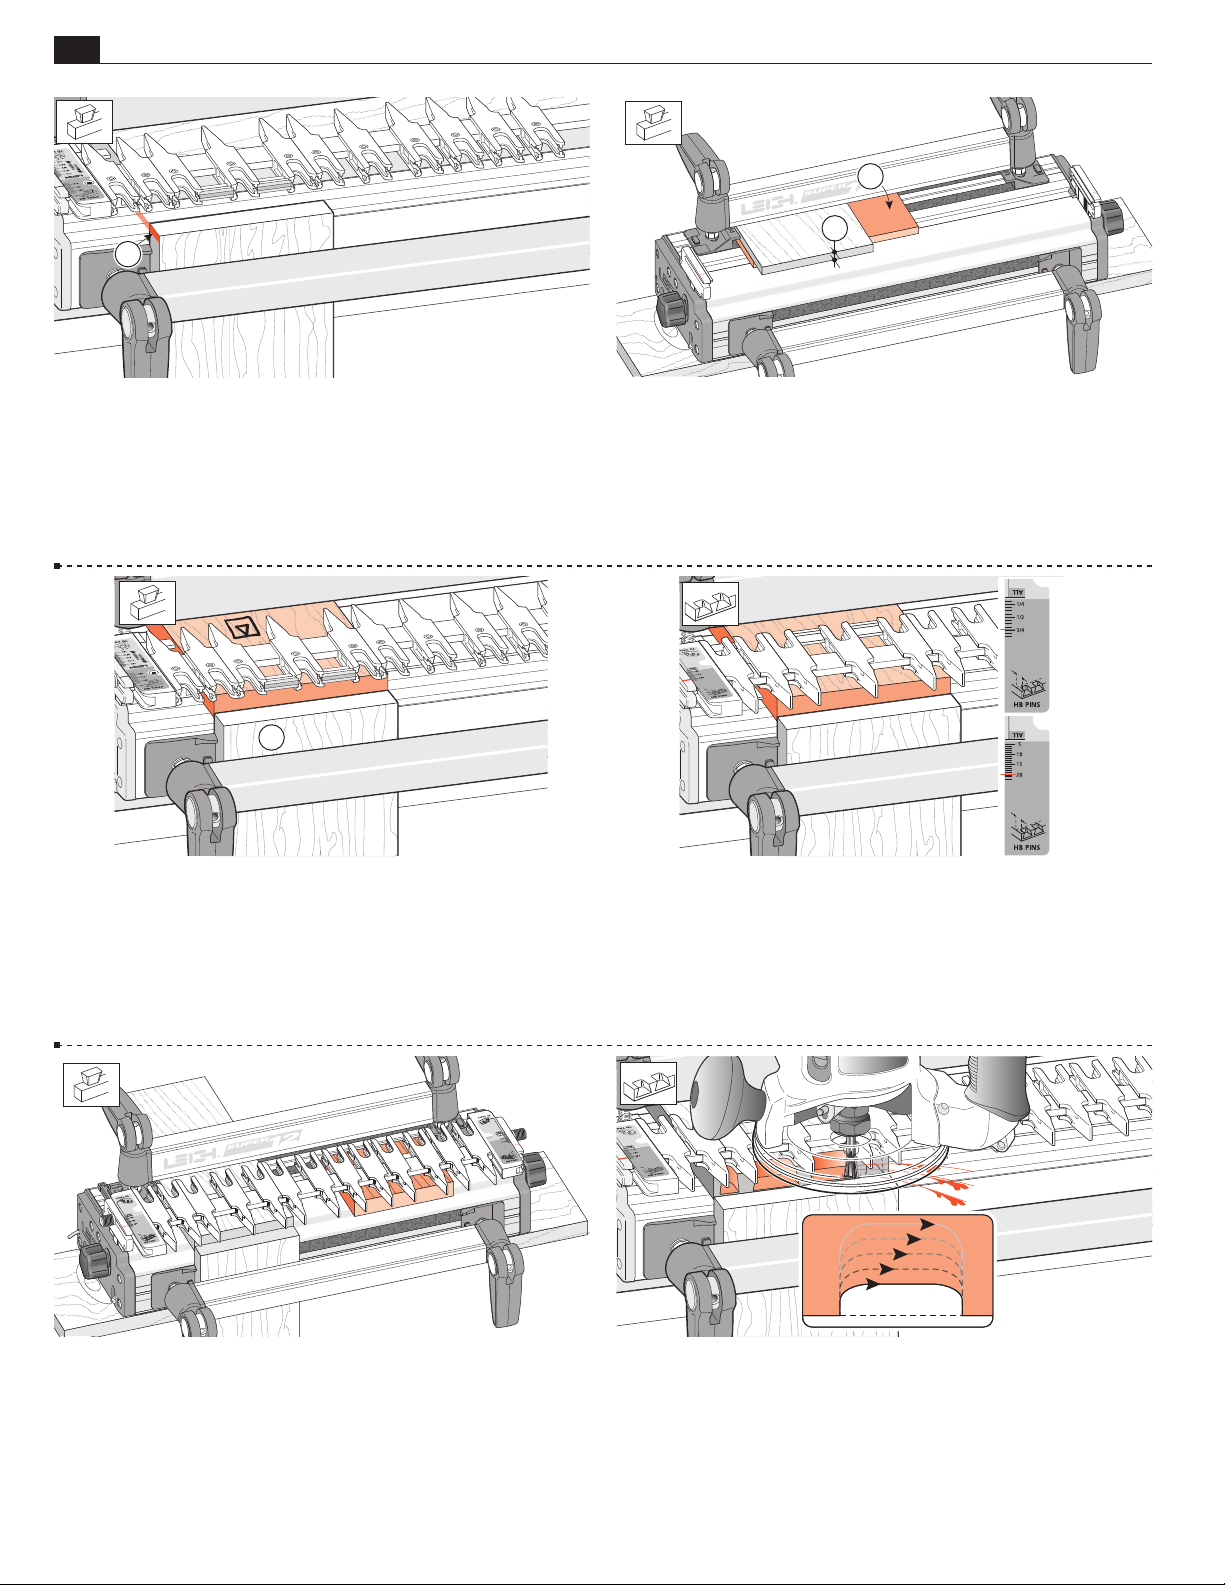
9-14 Ignoring the extreme outer guidefinger next to the scale
(which just supports the router), loosen enough of the adjacent guides to give the required pin socket layout. The half-pin
guidefinger position illustrated will give a half-pin socket profile
like that shown (dotted lines).
9-16 Remember to tighten any loose guidefingers. Lower the
finger assembly back onto the spacer board and workpiece. It
must touch the workpiece or the depth of cut will vary and the
joint won’t fit. The scale should be set on the tailboard thickness,
3
in this case
⁄4"[20mm].
9-15 If the gaps between the guidefinger tails are wider than about
1
⁄8"[3mm], mark off and cut some pieces of bridge extrusion to
fit into the slots in the ends of the guidefinger tails. Cut the pieces
1
a "bare"
⁄8"[3mm] more than the distance between the fingers .
They are a firm friction fit.
After completing a project, save the bridge pieces for future use.
9-17 Attach the provided e7-Bush or a 7⁄16"[11,1mm] diameter
bush securely to the router. No guidebush adjustment is required
with half-blind dovetails.
Fit the selected dovetail bit to the router.
REMEMBER SAFETY!
2
1
9-18
level with the marked line . For the first light cut
Adjust the bit height until the bit tip is
move the router from right to left. Make sure you control it firmly,
because it is driven in this direction by the bit. Only the tip of
the bit should be cutting on the first cut
. This back or climb
routing leaves a very clean shoulder in side grain.
9-19 Now rout in and out from left to right following the guides
and bridge pieces to rout out the pin sockets, leaving the tails.
See Hints and Tips 15-11.
Page 40
34
Chapter 9 Sup er Jig -12-18-24 User Guide
1
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
2
1
9-20 Remove the test tail board, then clamp a scrap board in the
front of the jig so that the top edge projects above the top face
1
of the jig by about
⁄8"[3mm] . This will keep the scrap piece
below the path of the bit when routing the pin board.
Remove the spacer board from the rear clamp.
1
9-22 Flush Drawers Place a test pin board in the left rear clamp
against the side stop, its front end edge flush to the vertical board,
the inside face
of the drawer front away from the jig body. The
i
pin board is now positioned with the edge to be routed flush with
the jig’s front face, correctly registered for the scale readings. For
rabbeted drawer fronts, see Chapter 11.
9-21 If you're mounting Thin Pin Boards:
Minimum recommended pin board thickness is 1⁄2"[13mm].
3
Remember, No.128-8 bits rout at
⁄8"[9,5mm] deep. If you rout
a pin board less than minimum thickness , you need to pack
1
the board up from the jig body. We suggest a piece of
⁄4" to 3⁄8"[6
to 9mm] plywood for this purpose .
9-23 Rotate the finger assembly to
HB PINS mode. Set
h
the HB pins scale equal to tail board thickness (i.e., same setting as
3
tails: this example,
⁄4"[20mm]). HB pins and HB tail scales are
always set to tail board thickness. Make sure the finger assembly
is flush and level on the pin board. The guidefingers must touch
the pin board or depth of cut will vary, causing poor joint fit.
9-24 If you have difficulty leveling the finger assembly on a narrow workpiece, place a board the same thickness as the pin board
under the other end of the finger assembly, but not in the rear
clamp.
9-25
from left to right. Do not back-rout on end grain.
Rout out the waste between the pins. Rout each space
If the bit enters on the right side of the opening there will be
a very strong pull to the left, so… rout each opening in at least
three or four passes, left to right.
Page 41
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
Chapter 9Sup er Jig -12-18-24 User Guide
35
1
2
90
o
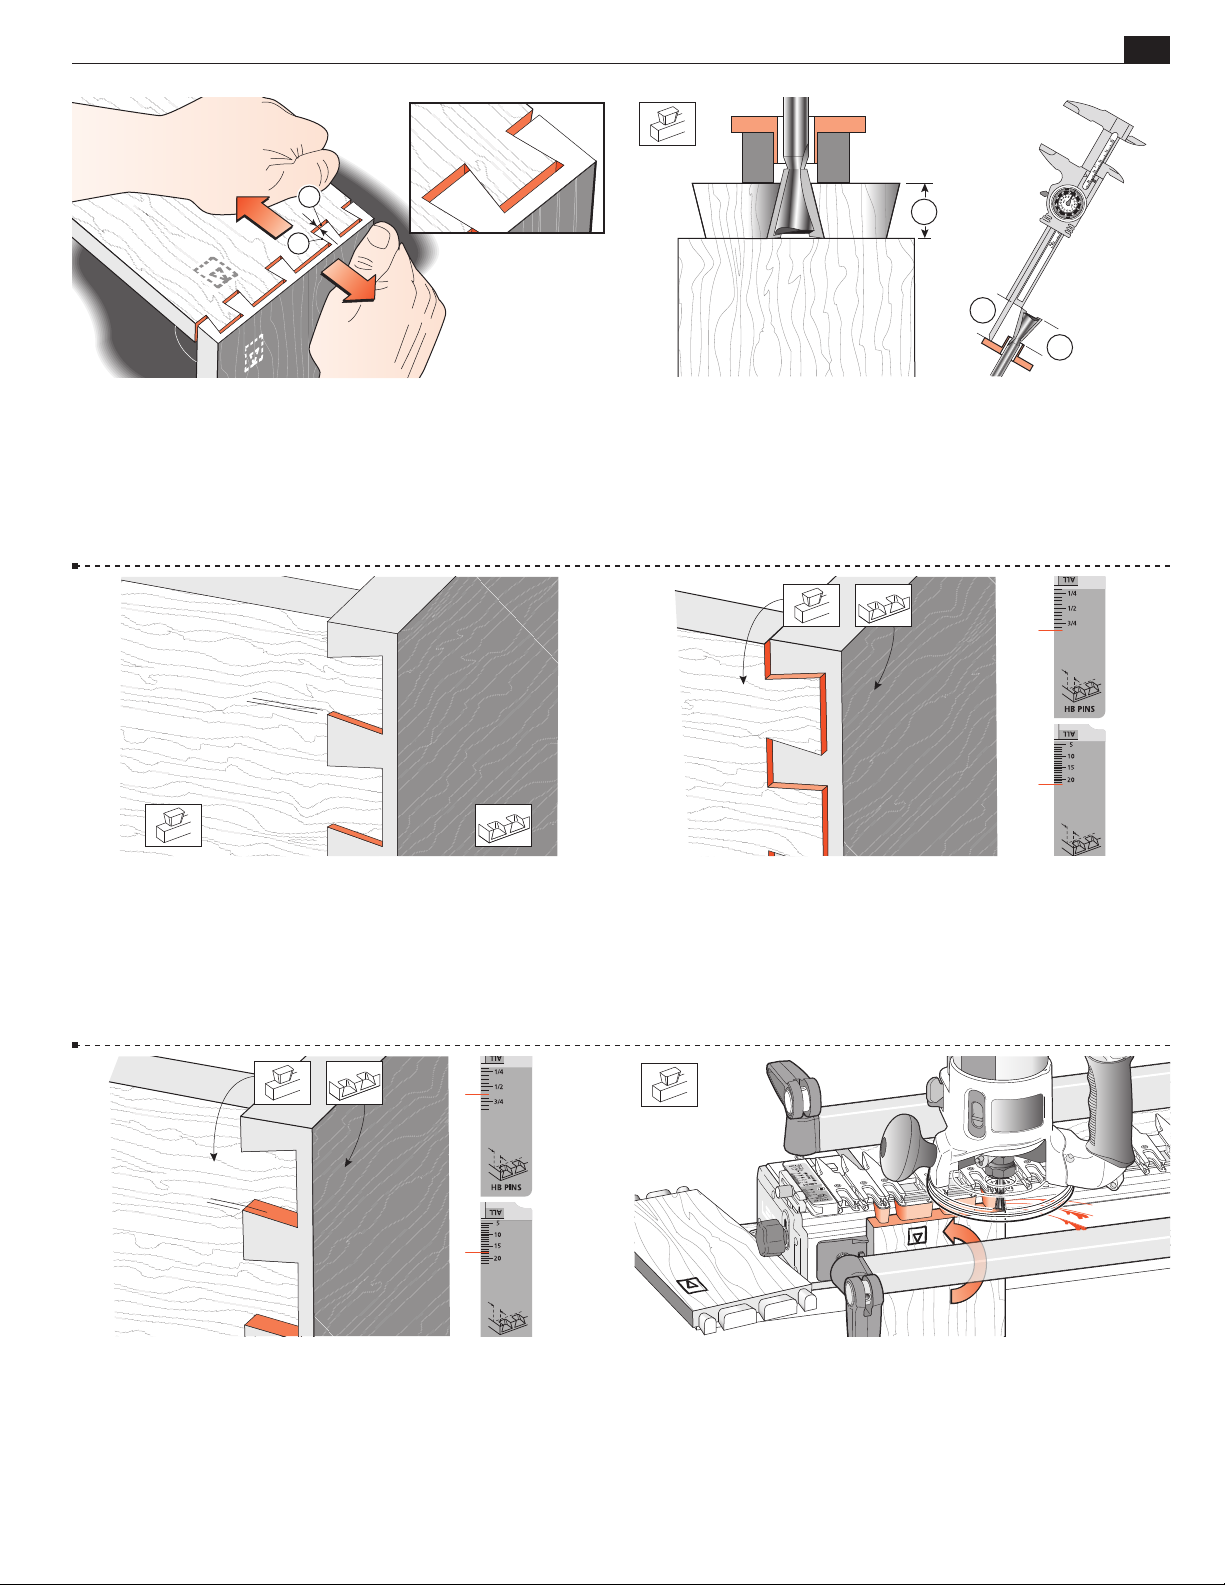
9-26 Remove the pin board and test the joint for fit. If the joint is
loose, as shown here, you need to lower the bit by the same amount
as the gap at the bottom of the pins (when the pins are pulled
against the socket sides ). If the joint is too tight, raise the bit
slightly. Test again. You cannot rout the same board twice with a
dovetail bit, so use two fresh board ends for each test.
1/64[0,3mm]
1
3
2
9-27 Keep the test tail board that fits well, and mark it with the
number of the bit you used to rout it. For quick set-up next time,
clamp this tail board in the jig as a depth-of-cut gauge
to show
how far to lower the bit. Better yet, measure the bit projection
from the end of the guidebush or guidebush flange and
record this for fast set-ups in future.
9-28 When you have the proper tightness of fit, check the flushness. The tails should be under flush to the pins by no more than
1
⁄64"[0,3mm] to allow for cleanup (exaggerated here). Any concen-
tricity errors in the collet and guidebush on different routers will
affect this tolerance.
1/64"[0,3mm]
9-30 If the tails fit in too far past the pins ends, set the
h
HB
PINS scale toward the operator by the amount required. These
adjustments for “flushness” are made only in the
h
HB PINS
mode.
9-29 If the tails stand out from the pins, set the
h
HB PINS
scale away from the operator by the amount required.
9-31 To make a box, rout all four ends of the tail boards, keeping
the inside face
of the tail boards away from the jig.
i
Page 42
36
Chapter 9 Sup er Jig -12-18-24 User Guide
VARIABLY SPACED HALF-BLIND DOVETAIL PROCEDURES
Y
A
X
A
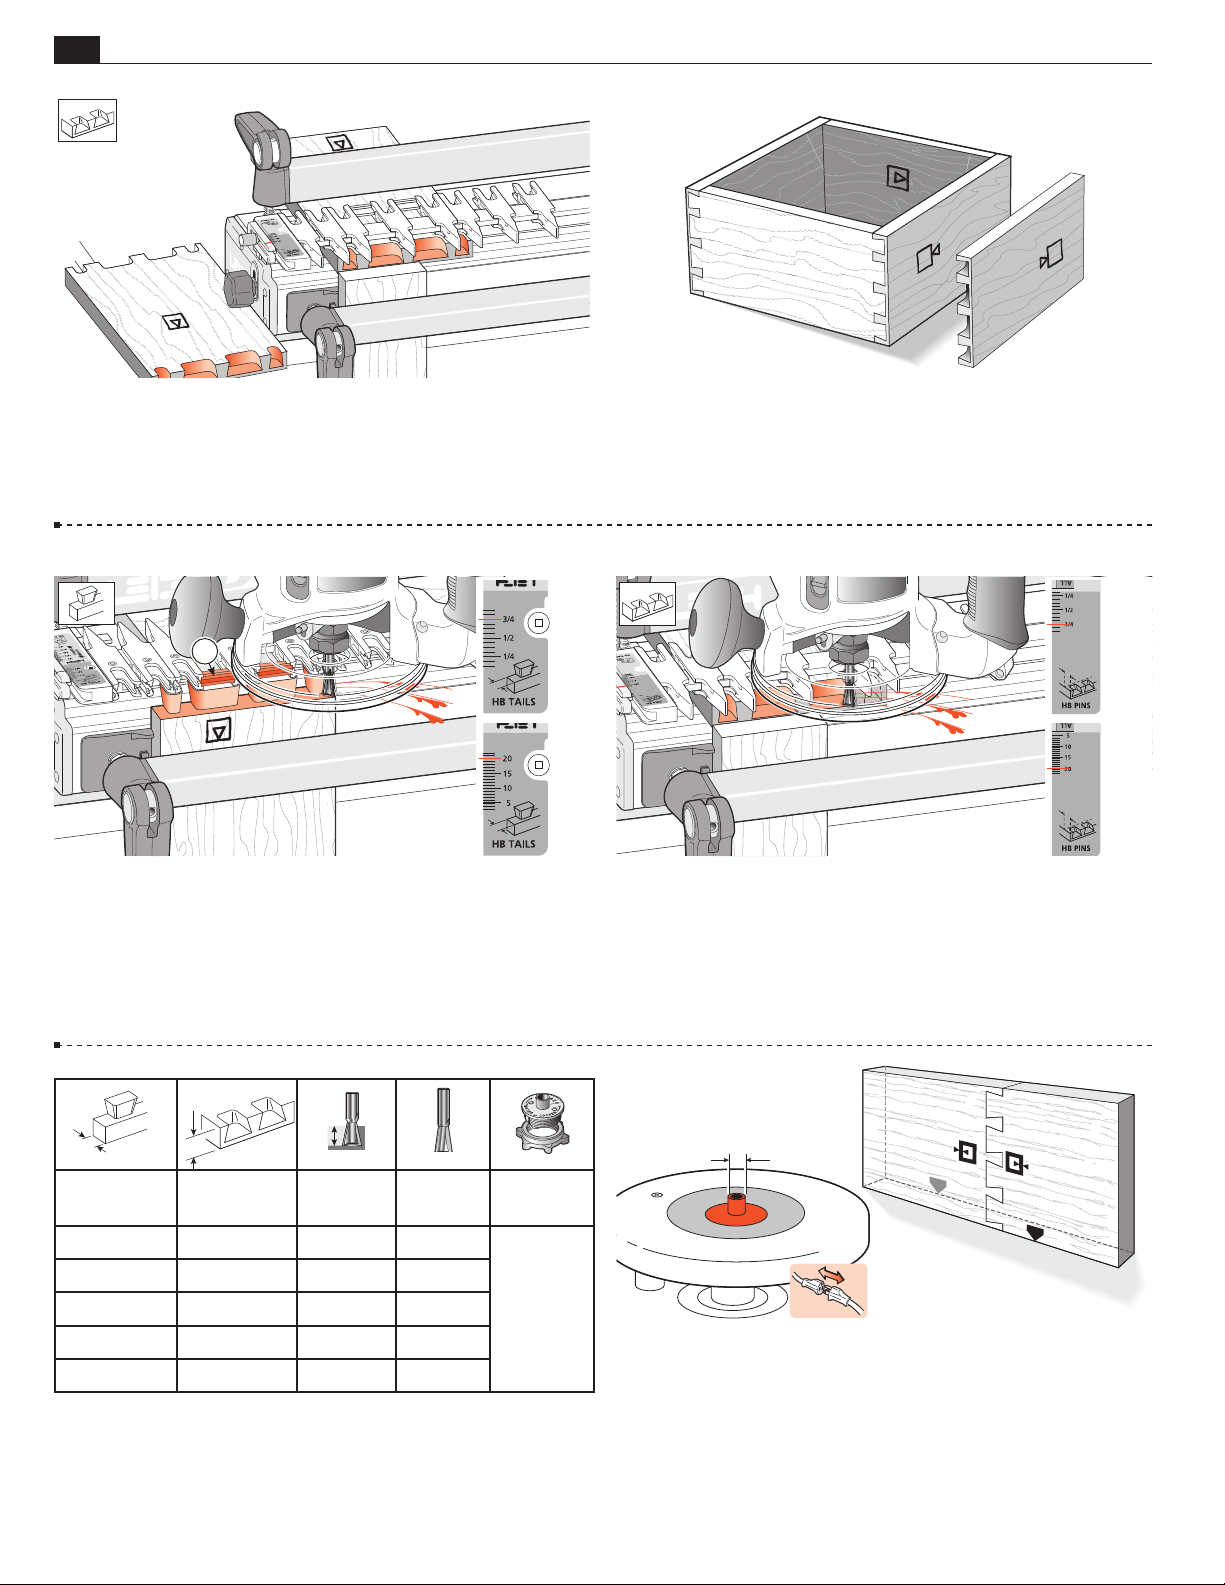
9-32 Rout all four ends of the pin boards keeping the inside
face i of the boards away from the jig.
Note: When making drawers you may prefer to use through dovetails
on the rear corners.
QUICK REFERENCE REMINDERS
1
9-QR1 Half-blind (HB) tails: Drawer sides (tailboards) are
clamped vertically in the jig. The inside face i of the drawer
side goes away from the jig body. The finger assembly is in the
HB TAILS mode, set to the thickness of the drawer side. Use
H
bridge pieces where required .
X
Y
9-33 Assemble the box. As with through dovetails, it doesn't
matter which edge of any of the boards are at the top or bottom,
the box will still fit together e.g. pin board “A” can be up either
way.
9-QR2
Half-blind (HB) pins: Drawer fronts (pinboards) are cut
with the board clamped horizontally in the jig. The inside face i of
the drawer front faces away from the jig body. The finger assembly
is in the
HB PINS mode, and again set on the thickness of
h
the drawer side (but adjusted for a flush fit, see 9-28 to 9-31).
Thickness of
Tail Board
up to 1"[26]
up to 1"[26]
up to 1"[26]
up to 1"[26]
up to 1"[26]
Thickness of
Pin Board
7
/8" -1" [22]
3
/4" -up [20]
5
/8" -up [16]
9
/16" -up [14]
1
/2" -up[12]
Depth of
Cut
3
~
/4" [19]
5
~
/8" [16]
1
~
/2" [13]
7
~
/16" [11]
3
~
/8" [9]
Dovetail
Bit
No.80-8
No.101-8 e7-Bush
No.112-8 or
No.120-8
No.128-8 guidebush
Guidebush
Diameter
~‚7
/16" [11,1]
7/16"[11,1mm]
9-QR3 On the Leigh Superjig, all half-blind dovetails are routed
using the e7-Bush or a 7⁄16"[11,1mm] diameter (min. depth 1⁄4" see
page 67) bush. Instructions for end-on-end dovetails are at www.
leighjigs.com/support.php. Scroll down Bulletins to “Superjig/
D1600 End on End Dovetails”.
■
Page 43
SUPERJIG - CHAPTER 10
Single Pass
Half-Blind Dovetails
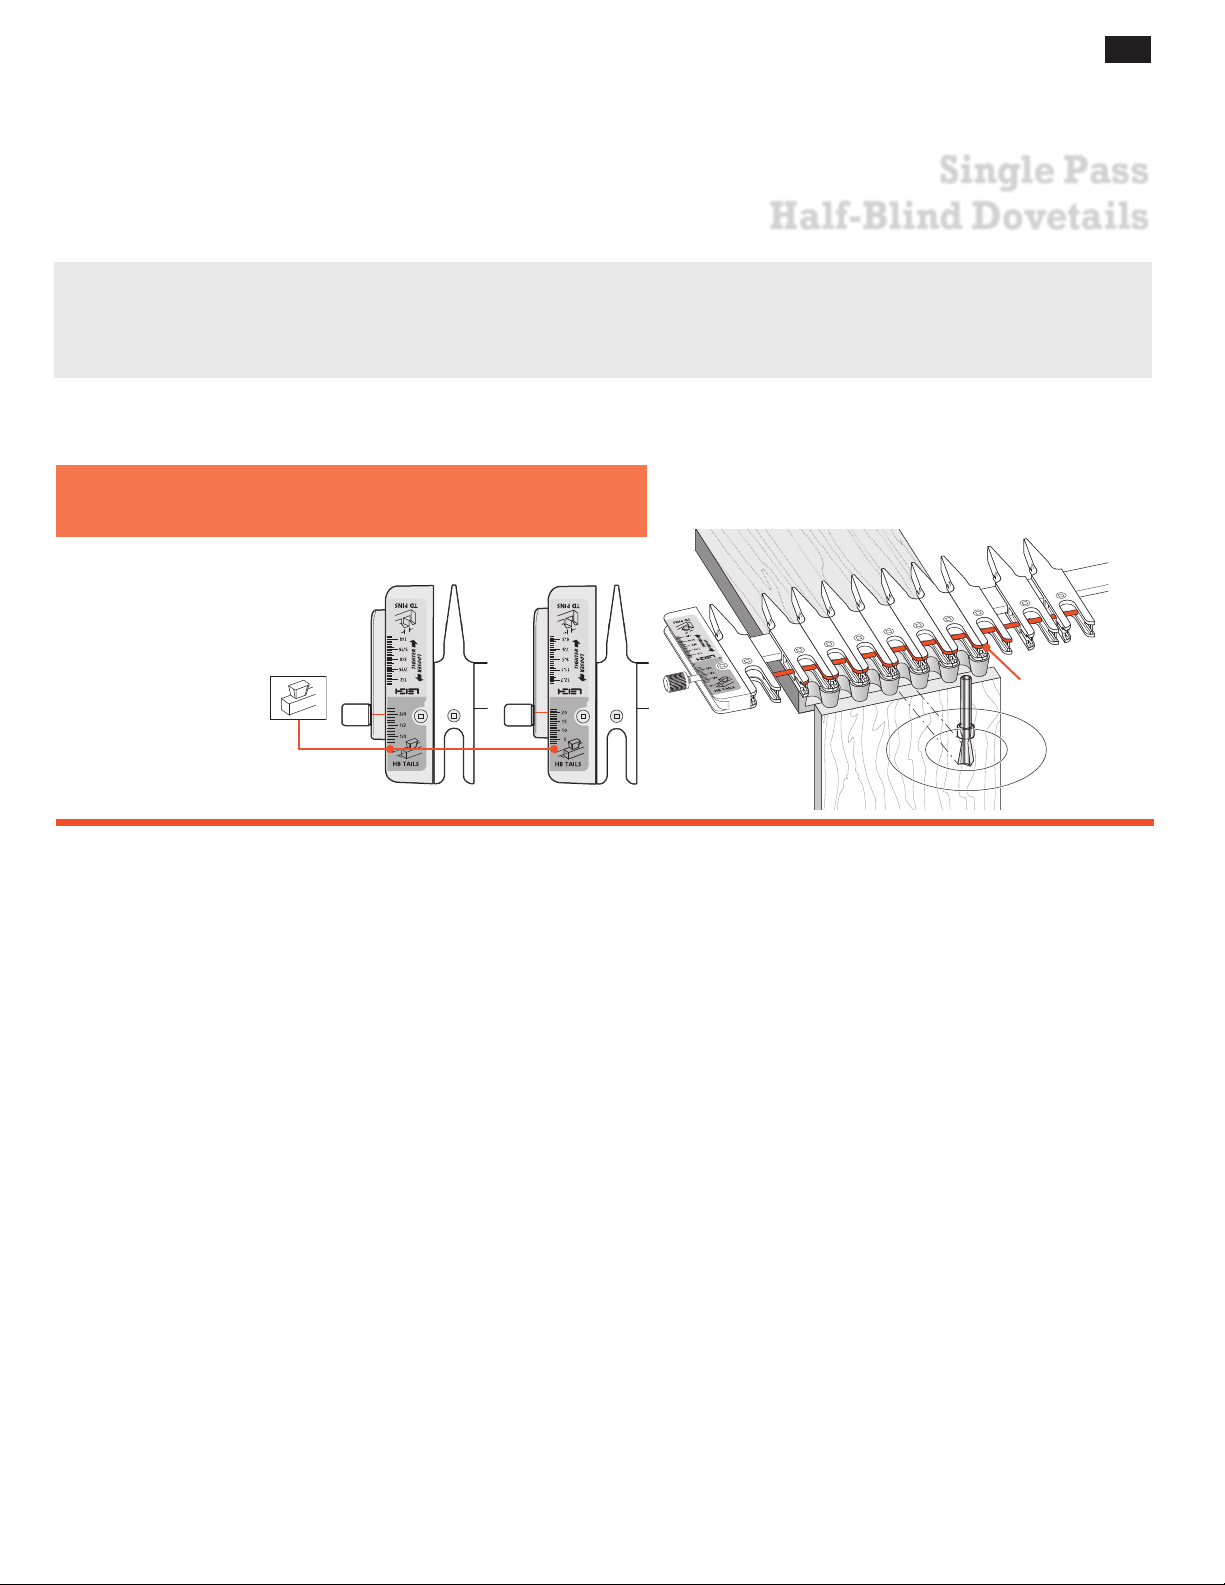
Why rout “single pass” dovetails on a variably spaced Leigh jig? Well, you just may need to reproduce or restore a
late 19th or early 20th century drawer which has similar, machine made joints. Or, if you are making a lot of drawer
boxes and are not so concerned with the traditional “hand-cut look”, then routing both drawer fronts and sides
together does go a little faster.
Only one mode is required:
Half-Blind Dovetail Tails (HB TAILS) mode
37
MODE ICONS
Illustrations in this user
guide include the correct
rent instruction. The
icons are also used in
the instruction text.
Inches
Millimeters
Active
Guide Surfaces
Page 44
38
" [3,2mm] Min.
Board Thickness
Board Thickness
" [3,2mm] Min.
Chapter 10 Sup er Jig -12-18-24 User Guide
1
6
3
Depth
8
of Cut
4
Depth
7
of Cut
22
5
SINGLE PASS HALF-BLIND DOVETAILS
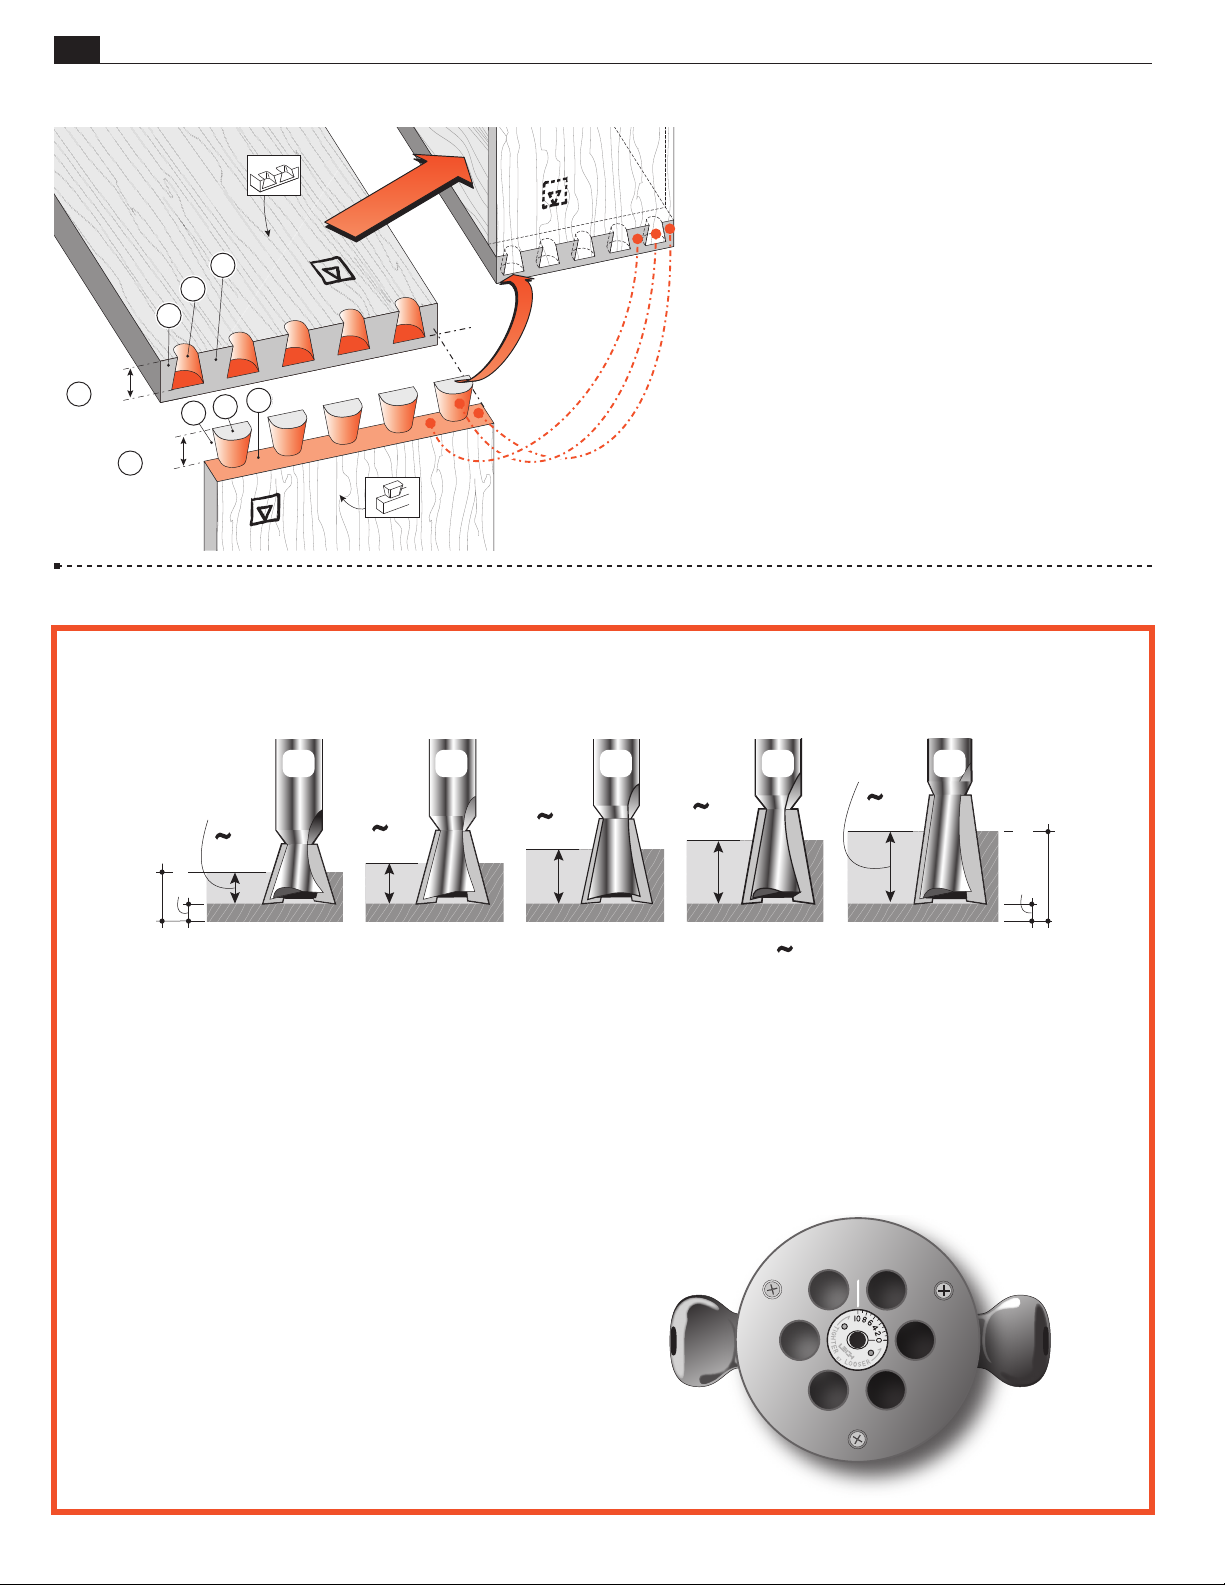
10-1 Single Pass Half-Blind Dovetail
Terminology:
Pins
h
Pin sockets
Half-pins
Half-pin sockets
Tails
➆
➇
H
Tail sockets
Depth of Cut (tails)
Depth of Cut (pins)
The pins fit in the pin sockets. Joints almost always
begin and end with a half-pin as shown.
10-2 Cutting Depth for Single Pass Half-Blind Dovetails
DEPTH
OF CUT
1
"
/
2
[12,35mm]
80-8
8˚
DEPTH
OF CUT
7
"
/
32
[5,56mm]
8
/
1
Note: Add at least
128-8
18˚
120-8
9
"
/
32
[7,13mm]
14˚
1
⁄8"[3,2mm] to the depth of cut for board thickness.
3
[9,52mm]
112-8
7
"
/
8
12˚
/
[11,1mm]
101-8
"
16
10˚
Symbol for “approximately”
IMPORTANT! Bit depths of cut for “single pass” dovetails
are not the same as for variably spaced joints.
Depth of cut must be as specified for each of the five
•
bits shown above. Exception: See fig.11-26. Note: Leigh
Raising the bit above its specified cutting depth will
•
result in loose joints and may damage the jig, bit and/
or guidebush. A lower setting will result in tighter
joints that may not fit together.
Fit the provided Leigh e7‑Bush to the router as shown
•
below and set at No.10, or use a standard 7⁄16"[11,1mm]
1
guidebush (min. barrel depth
/4" see page 67).
8
/
1
Small Depth of Cut adjustments will allow for joint
•
fit tightness. See why in Steps 9-3 to 9-5.
Choose one of the five, 1⁄2"[12,7 mm] diameter dovetail
•
bits shown above.
Page 45
SINGLE PASS HALF-BLIND DOVETAILS
5
4
1
2
3
8˚
18˚
Chapter 10Super Ji g-12-18-24 User Guide
1
39
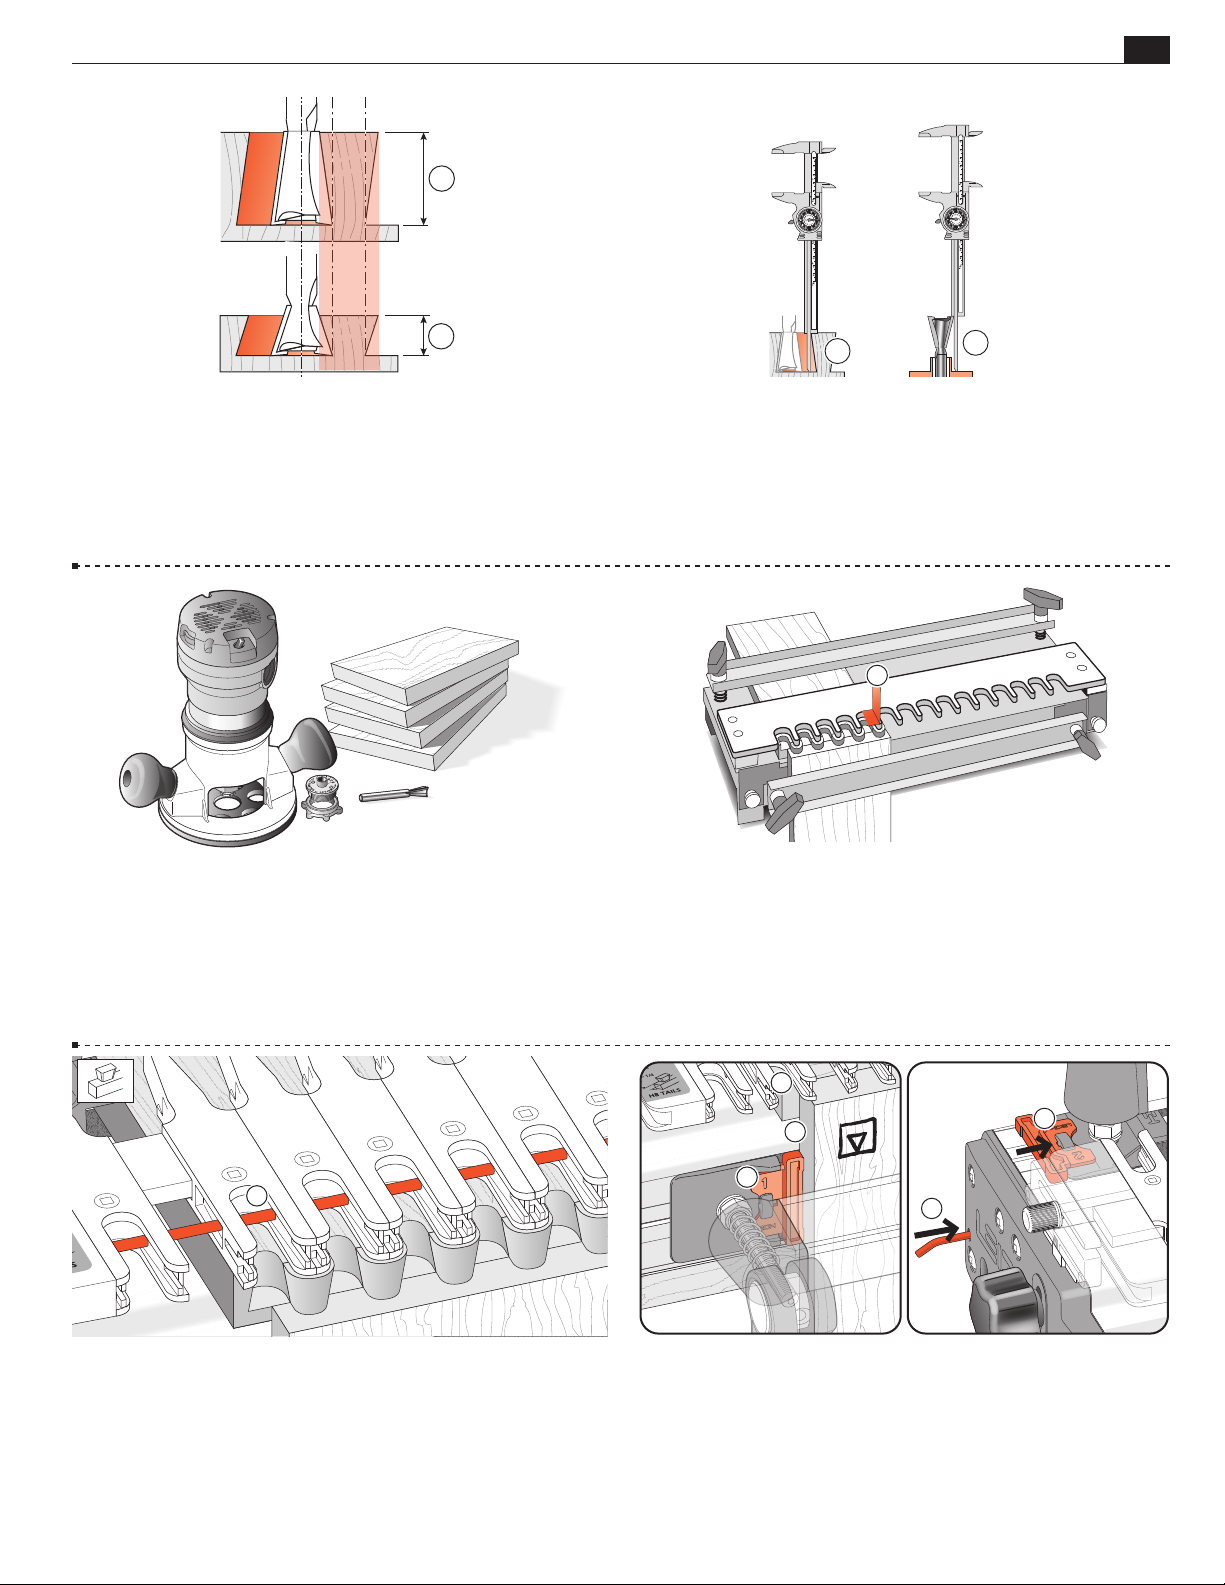
2
10-3 Bit Angle and Depth of Cut. Half-blind pins and tails
are routed with the same dovetail bit, the same guidebush, and
the same depth of cut. A different depth of cut requires a different angled bit. Leigh offers five different angled dovetail bits for
a range of cut depths. A lesser angle, say 8˚, for a deeper cut ; a
greater angle, say 18˚, for a shallower cut .
10-5 Routing a Test Joint You need a router, the e7‑Bush set
1
at No.10, the 80-8
thick pin boards and two
routs at a shallower ~
⁄2"[12,7mm] 8˚ dovetail bit, two 3⁄4"[19mm]
1
⁄2" thick tail boards. The No.80-8 bit
1
⁄2"[13mm] depth on single pass dovetails
than on regular variably spaced joints. For this test, start with the
No.80-8 bit projecting 1"[26mm] from the router base.
1
2
10-4 Cumulative plus/minus tolerances in routers, bits and
guidebushes, make it impossible to state exact bit depth for firsttime precision fit. All dovetail jigs require trial and error tests to
attain a fine fitting joint. The good news; we give a starting depth
for each bit. Test and measure the successful ‘Best fit’ depth of
cut or bit projection and record for future first-time fits.
1
10-6 This is a typical fixed template comb type jig. The comb
depth is usually dimensioned to suit the most popular drawer
1
side thickness of
⁄2"[12,7mm].
1
10-7 Superjig features two novel innovations.
A Stop Rod inserted through the fingers limits router travel to
allow the deep tail socket guides to function as a simple shallow
fixed comb.
10-8 The Spacer in the #1 position, slipped into the left-hand
front side stop correctly offsets drawer sides from drawer
fronts . The Spacer stays in place for the complete procedure.
The Stop Rod stores here and the Spacer here .
Page 46
40
Chapter 10 Sup er Jig -12-18-24 User Guide
SINGLE PASS HALF-BLIND DOVETAILS
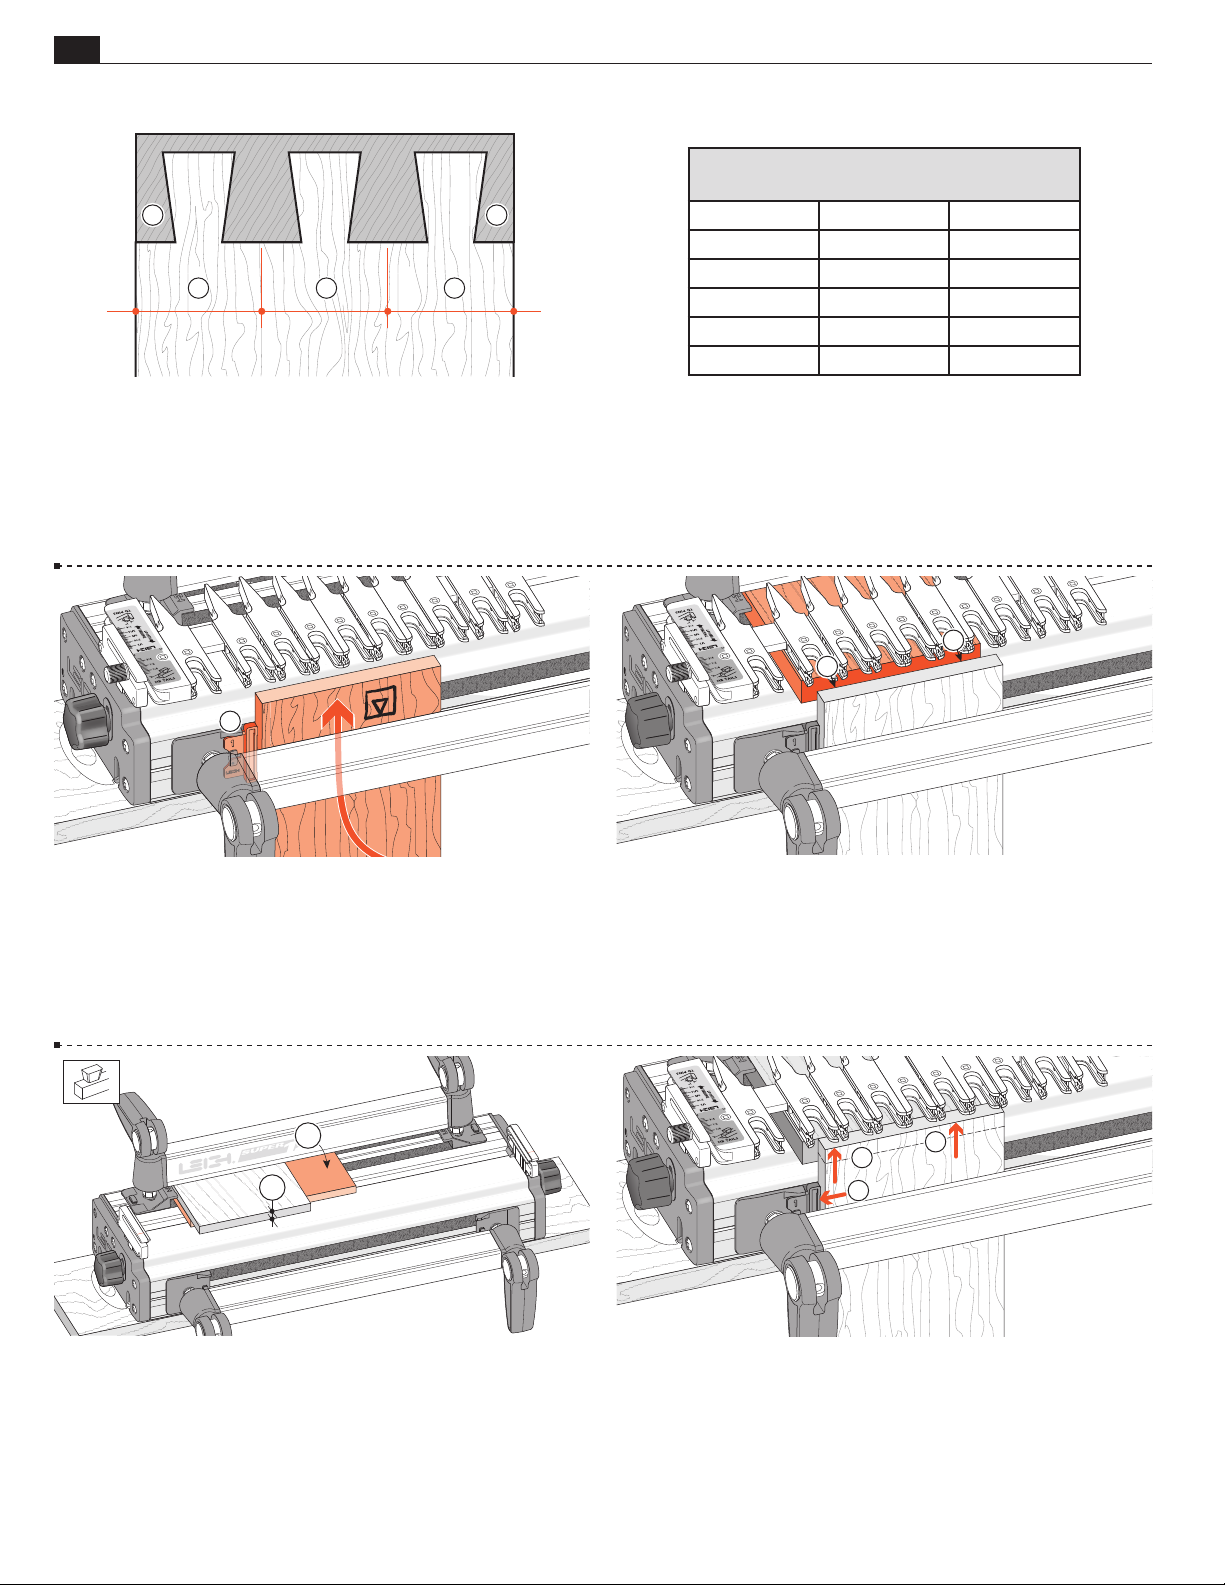
Board Width Chart
1
2 2 2
Add up to ¼" [6mm] or subtract up to 1/8" [3mm]
1
7
⁄8 [22] 6 1⁄8 [156] 1 1 3⁄8 [289] (SJ-18)
3
1
⁄4 [44] 7 [178] 12 1⁄4 [311]
5
2
⁄8 [67] 7 7⁄8 [200] 13 1⁄8 [333]
1
3
⁄2 [89] 8 3⁄4 [222] (SJ-12) 14 [356] (SJ-24)
3
4
⁄8 [111] 9 5⁄8 [244]
1
5
⁄4 [133] 10 1⁄2 [267]
10-9 Board Widths: To achieve equally sized half pins at each side of a fixed space joint, use chart width plus up to 1⁄4"[6mm],
1
or chart width minus up to
Example: the 7"[178mm] can be up to 7
1
⁄8"[3mm]. This chart covers boards up to maximum width for each jig.
1
⁄4"[184mm] or as small as 67⁄8"[175mm].
⁄4" thick drawer front,
⁄2" thick drawer side and #80-8 dovetail bit. Scale settings and depth of cut will vary
1
1
10-10 Slip the Spacer onto the left hand front side stop , note:
HB Tails
H
mode, clamp a drawer side in the front left side, against the Spacer
and the top end edge slightly above the jig body top.
⁄16" to
⁄16"[6 to 14mm].
2
1
10-12 If you're mounting Thin Pin Boards:
1
Minimum recommended pin board thickness is
3
Remember, No.128-8 bits rout at
⁄8"[9,5mm] deep. If you rout
⁄2"[13mm].
a pin board less than minimum thickness , you need to pack
1
the board up from the jig body. We suggest a piece of
⁄4" to 3⁄8"[6
to 9mm] plywood for this purpose .
10 -11 Place the drawer front (from 1⁄2" to 1" thickness [16 to
25mm]) in the rear clamp. Clamp with the side edge against the
left rear side stop, front end edge touching flush across the rear of
the front board . Lower the finger assembly to the drawer front.
! Board edges must be square.
1
2
1
10 -13 Re-set the drawer side in the front clamp so that its top
edge touches the guide fingers and is perfectly flush with the top
face of the drawer front and the left edge is against the Spacer .
! Board edges must be square.
Page 47
SINGLE PASS HALF-BLIND DOVETAILS
1
Chapter 10Super Ji g-12-18-24 User Guide
1
2
41
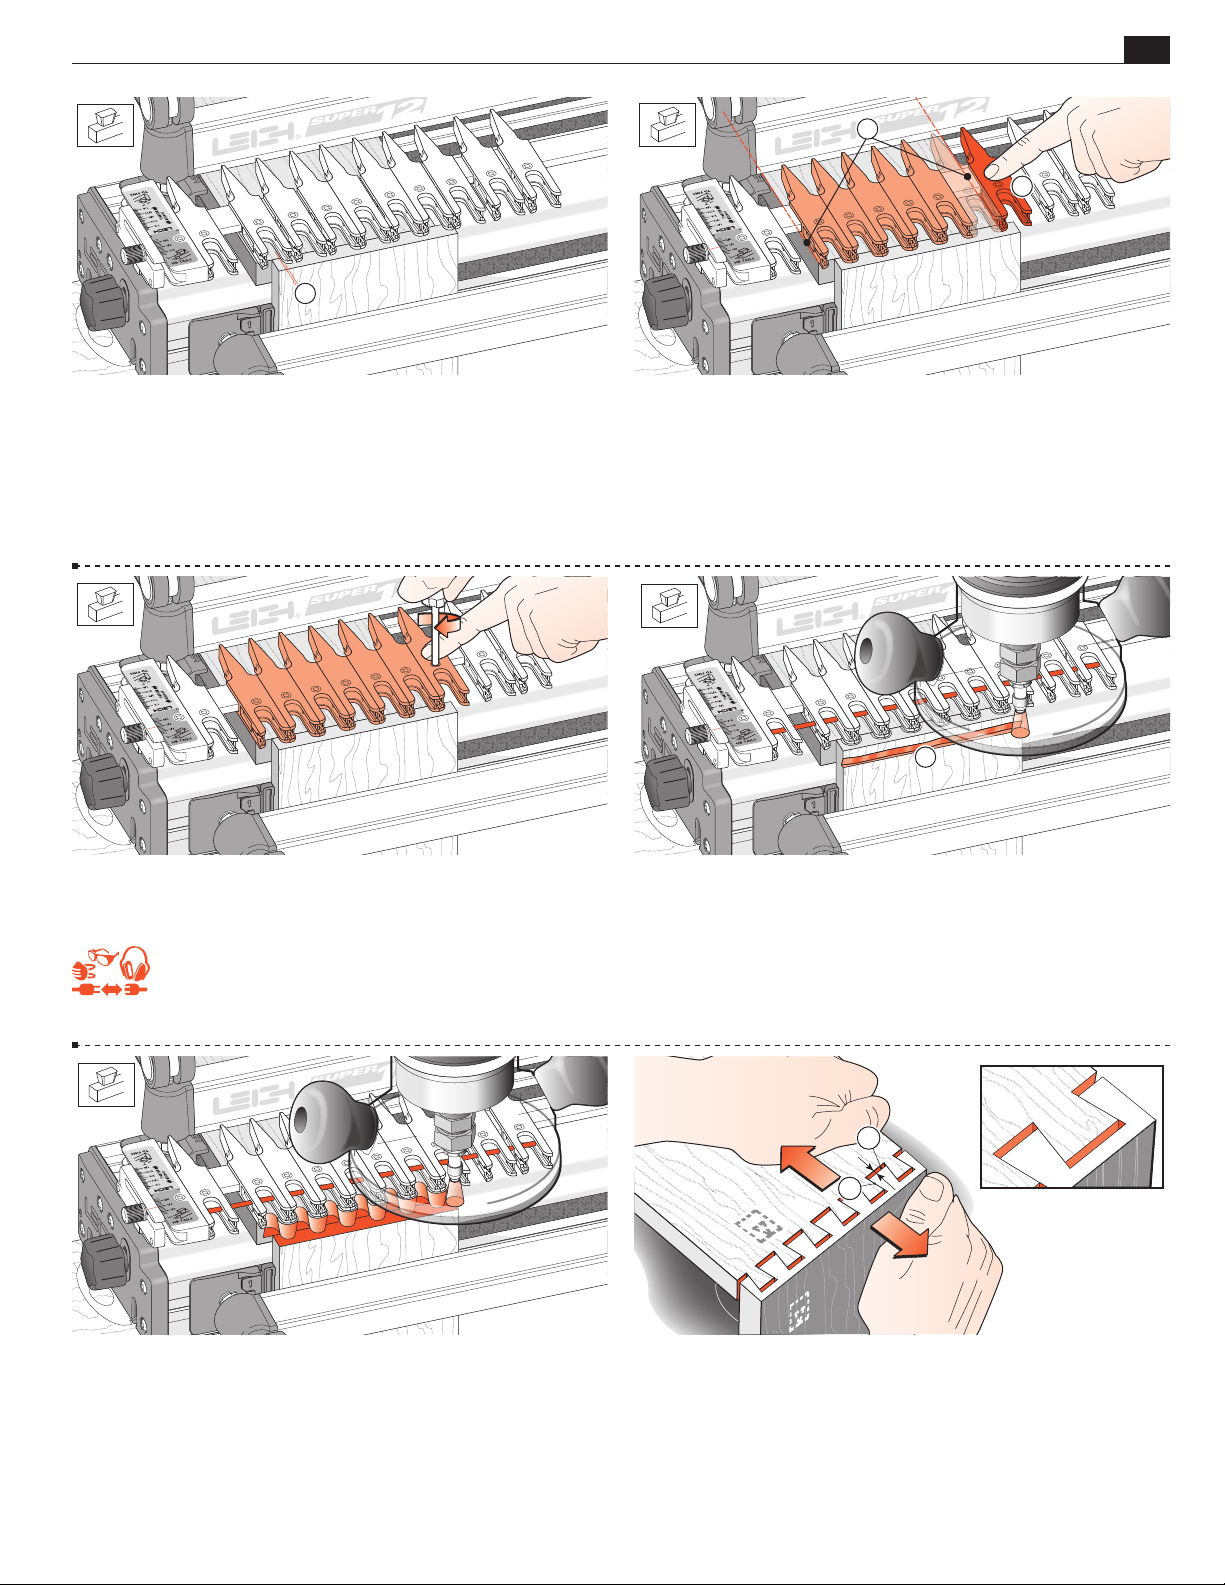
10 -14 With the scale set on 1⁄2"[12,7mm], raise the finger assem-
1
bly about
⁄16"[2mm] above the drawer front . The scale is always
set on the 1/2" mark when using the stop rod. See 10-26 for Drawer
10 -16 Tighten the finger’s screws. Move any spare fingers so
that they will support the router and tighten all loose fingers.
Lower the assembly flat onto the two work pieces.
REMEMBER SAFETY!
10 -15 Slide across enough guide fingers to cover the drawer
front width. Position fingers tight together and center the group
of fingers on the board .
Depending on the exact board width, the outer fingers will either
overhang, be inside, or flush with the board edges. Now add one more
finger to the right of the group for routing the drawer side.
1
10 -17 Insert the Stop Rod through the fingers.
For the first light cut move the router from right to left. Make
sure you control it firmly, because it is driven in this direction
by the bit. Only the tip of the bit should be cutting on the first
. This back, or climb routing, leaves a very clean shoulder
cut
when routing side grain.
10 -18 Now rout in and out from left to right. Follow the guides
into each finger opening to touch the stop rod. The pins, tails and
sockets are formed simultaneously.
1
2
90
o
10 -19 Remove the boards and test the joint for fit. If the joint
is loose, as shown here, lower the bit by the same amount as the
gap at the bottom of the pins when the pins are pulled against
the socket sides . If the joint is too tight, raise the bit slightly.
Test again. You cannot rout the same board ends again with a
dovetail bit, so use two fresh ends for each test.
Page 48
42
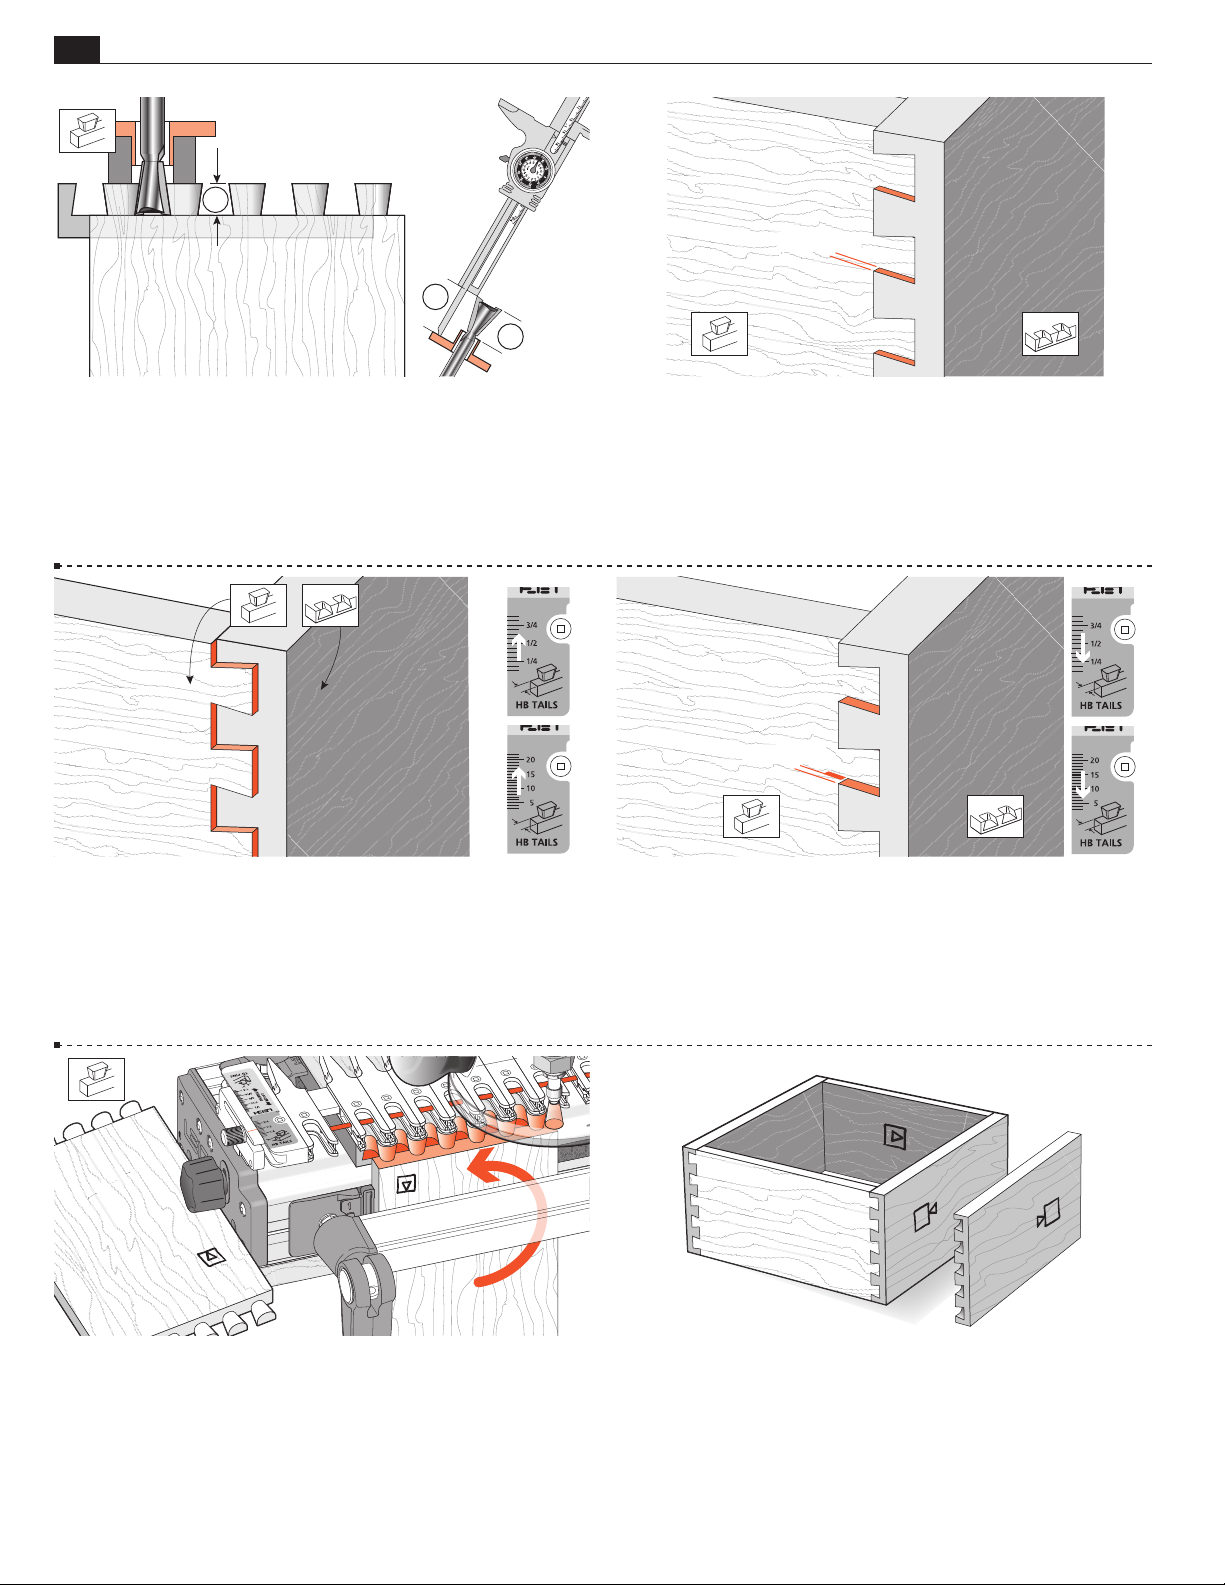
Chapter 10 Sup er Jig -12-18-24 User Guide
1
3
SINGLE PASS HALF-BLIND DOVETAILS
1/64[0,3mm]
2
10-20 Keep the test tail board that fits well, and mark it with
the number of the bit you used to rout it. For quick set-up next
time, clamp this tail board in the jig as a
to
show how far to lower the bit. Better yet, measure the bit projection from the end of the guidebush or guidebush flange and
record this for fast set-ups in future.
10-22 If the tails stand out from the pins, set the HHB TAILS
scale away from the operator by half the amount required.
10-21 When you have the proper tightness of fit, check the
flushness. The tails should be under flush to the pins by no more
concentricity errors in the collet and guidebush on different routers
will affect this tolerance.
1/64[0,3mm]
10-23 If the tails fit in too far past the pins ends, set the
HB TAILS scale toward the operator by half the amount
H
required.
10-24 To make a box, repeat the procedure four times, ensuring
that the drawer fronts, rears and sides are all rotated correctly in
the jig,
keeping the inside face i of the boards away from the
jig.
Y
A
X
Y
X
A
10-25 Assemble the drawer. As with through dovetails, it doesn't
matter which edge of any of the boards are at the top or bottom,
the drawer will still fit together e.g. pin board “A” can be up either
way.
Page 49
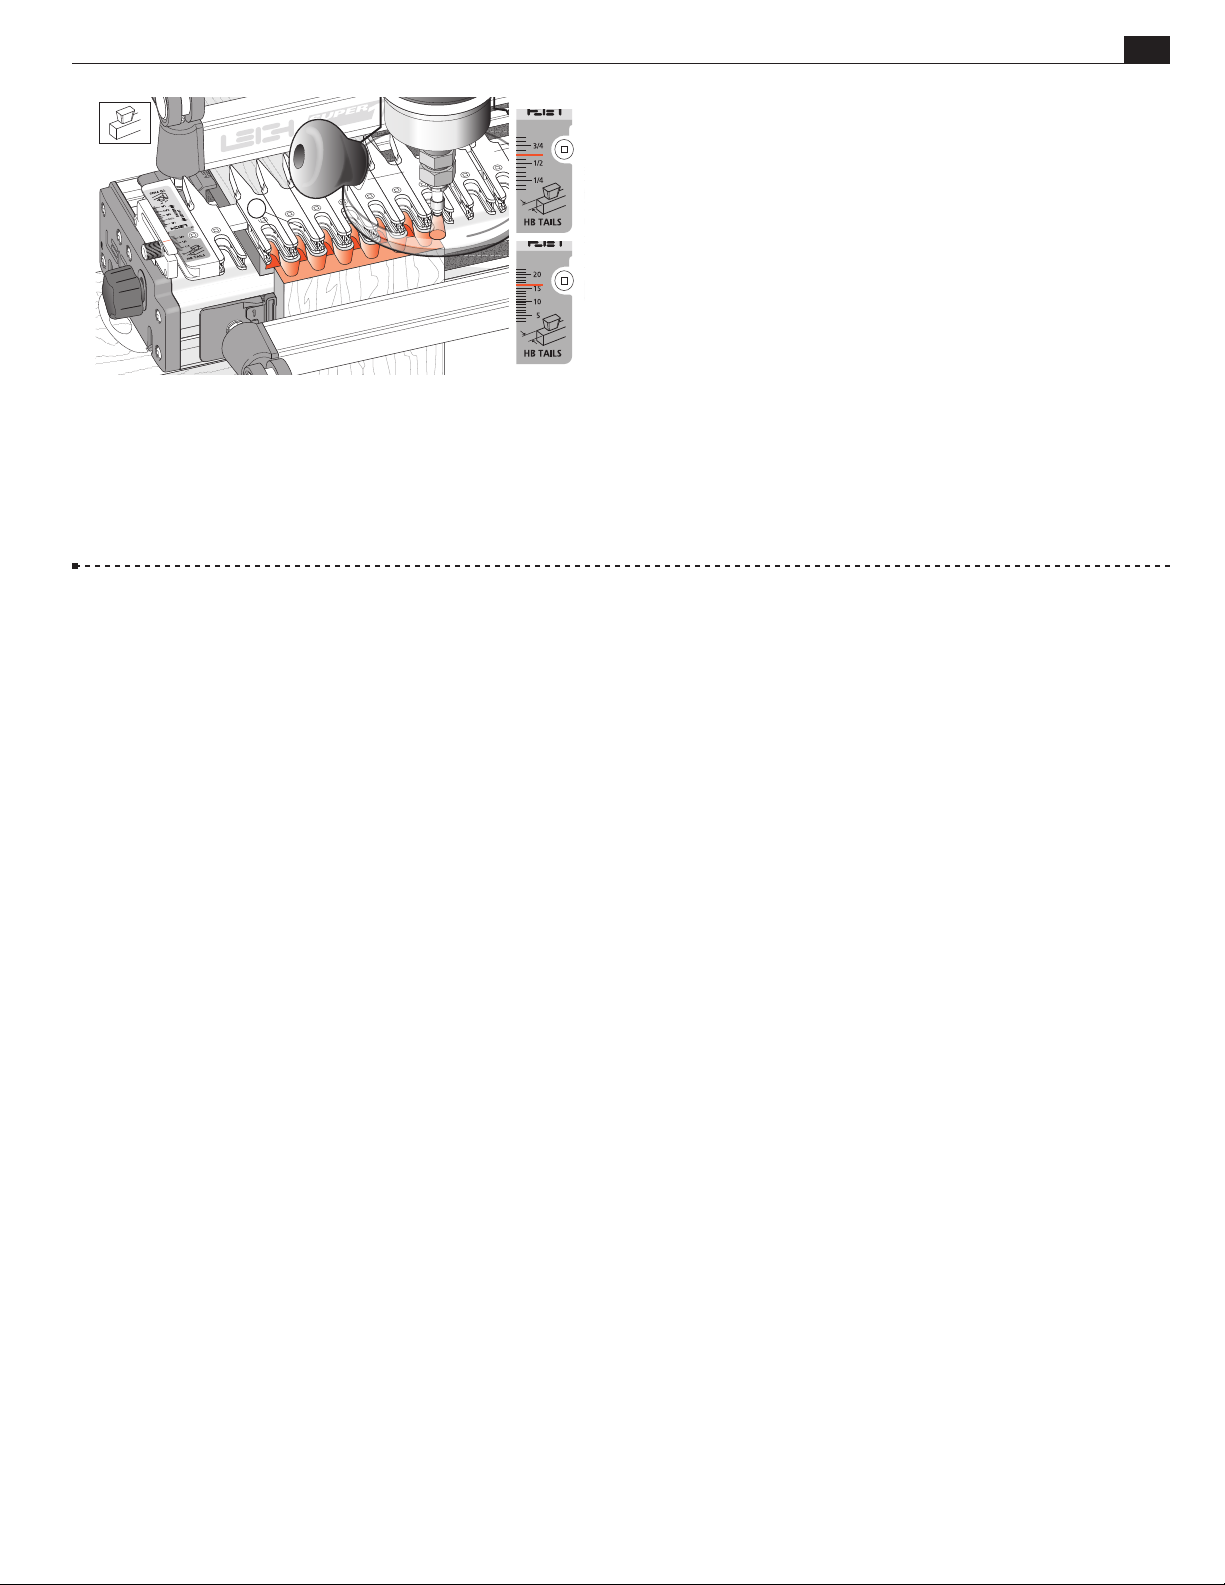
SINGLE PASS HALF-BLIND DOVETAILS
1
10-26 Tail Boards 5/8"[16mm] and thicker.
Use the same procedure to rout “single pass” dovetails with side
5
thicknesses from
⁄8" to 1"[16 to 25mm] except:
The stop rod is not used and the initial scale setting is 5⁄8"[16mm]
for all boards . Hint: Set the e7-Bush to lower than 10 for deeper
■
Chapter 10Super Ji g-12-18-24 User Guide
43
Page 50
44
Chapter 10 Sup er Jig -12-18-24 User Guide
SINGLE PASS HALF-BLIND DOVETAILS
Page 51
SUPERJIG - CHAPTER 11
2
3
Rabbeted
Half-Blind Dovetails
Before attempting rabbeted half-blind dovetails, first master the techniques of flush half-blind dovetails in
Chapter 9, Variably Spaced Half-Blind Dovetails.
Note: Rabbeted half-blind dovetails cannot be routed in a single pass – the lip of a drawer front makes it impractical,
as each piece would have to be routed separately, in which case it is easier to use the variably spaced method.
=
1
2
=
45
1
1
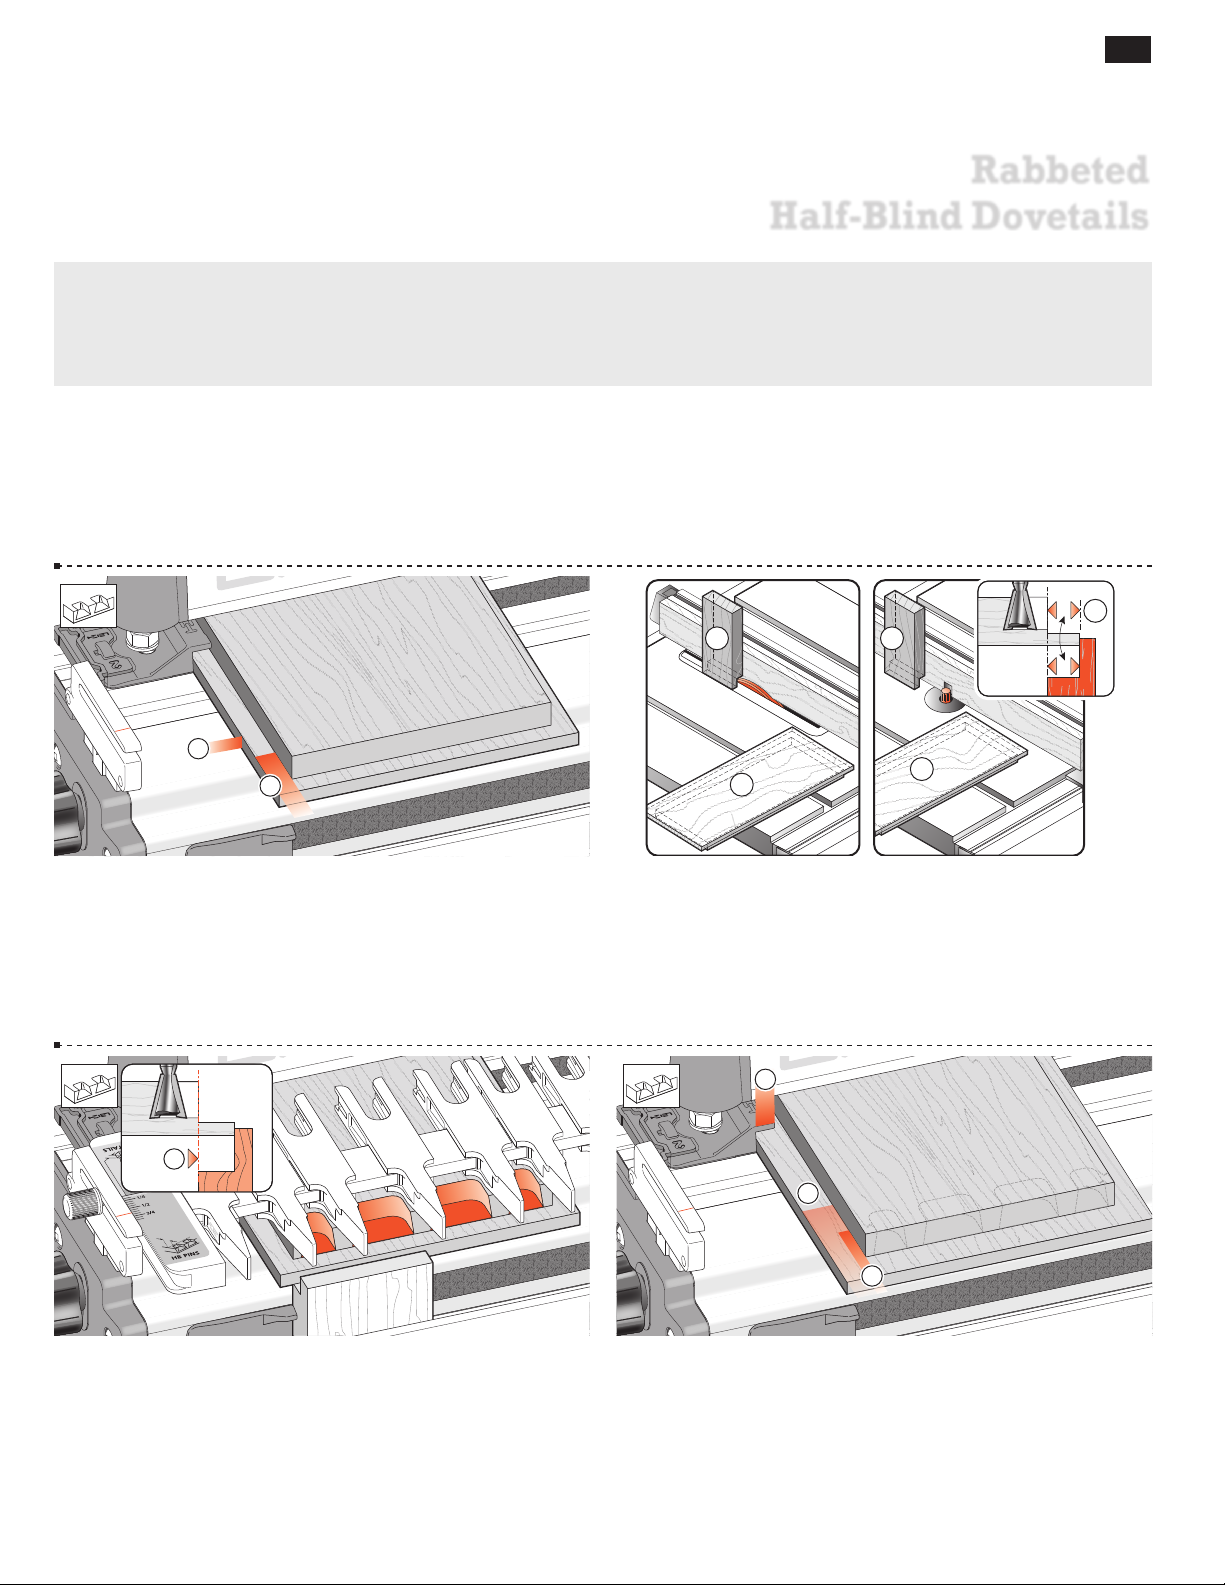
11-1 Provided the drawer front lip is
3
⁄8"[9,5mm] or less in each
direction , you can mount and rout rabbeted drawer fronts and
sides exactly the same way as flush drawer fronts, except...
1
3
11-2 Rabbeted Pins You will need to block the scrap stop in the
.
An easy accurate way to do this is to rabbet the end of the scrap
piece vertically over a dado blade or router bit at the same time
as you rabbet the drawer front (horizontally) .
2
1
3
11-3 This brings the pin ends exactly in line with the front jig
face , ensuring that the scale reading is accurate.
11- 4 If the rabbet width is greater than the top side stop width
3
⁄8" , the drawer side (tailboard) must be blocked away from
of
the front side stop (see 11-5) by exactly the width of the rabbet
3
minus
tailboard to be offset by an additional
⁄8" . For example, a 5⁄8" rabbet would require the
1
⁄4" .
Make a spacer block of the required width and…
Page 52
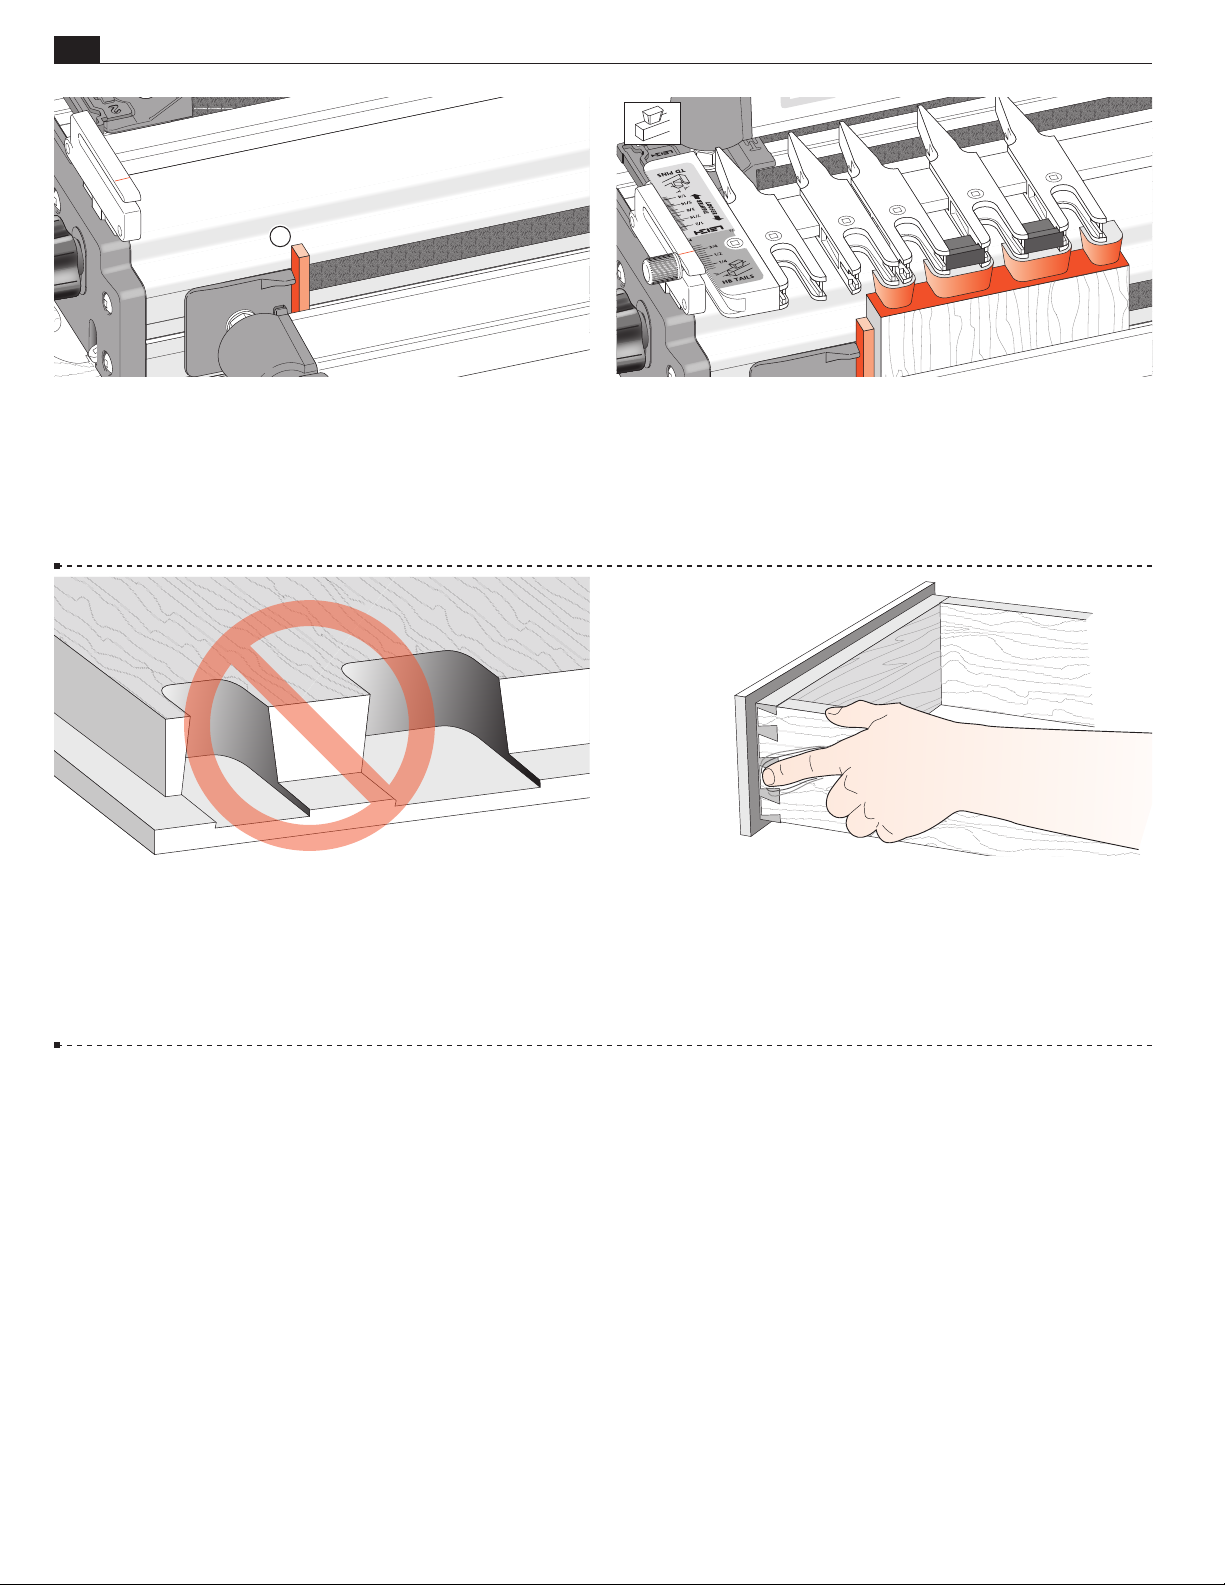
46
Chapter 11 Sup er Jig -12-18-24 User Guide
3
RABBETED HALF-BLIND DOVETAILS
11- 5 Stick the block to the jig face with double-sided tape,
making sure it touches the side stop.
11-7 Make sure you select a dovetail bit that has a working depth
rabbet.
11- 6 The drawer side will now be stepped in from the side stop
by the width of the rabbet, bringing the sockets in line with
the pins.
11- 8 It is difficult to clean up the drawer sides and front corner
after assembling a rabbeted drawer, so make sure the fit is flush
before you complete the drawers See 9-28 to 9-30.
■
Page 53
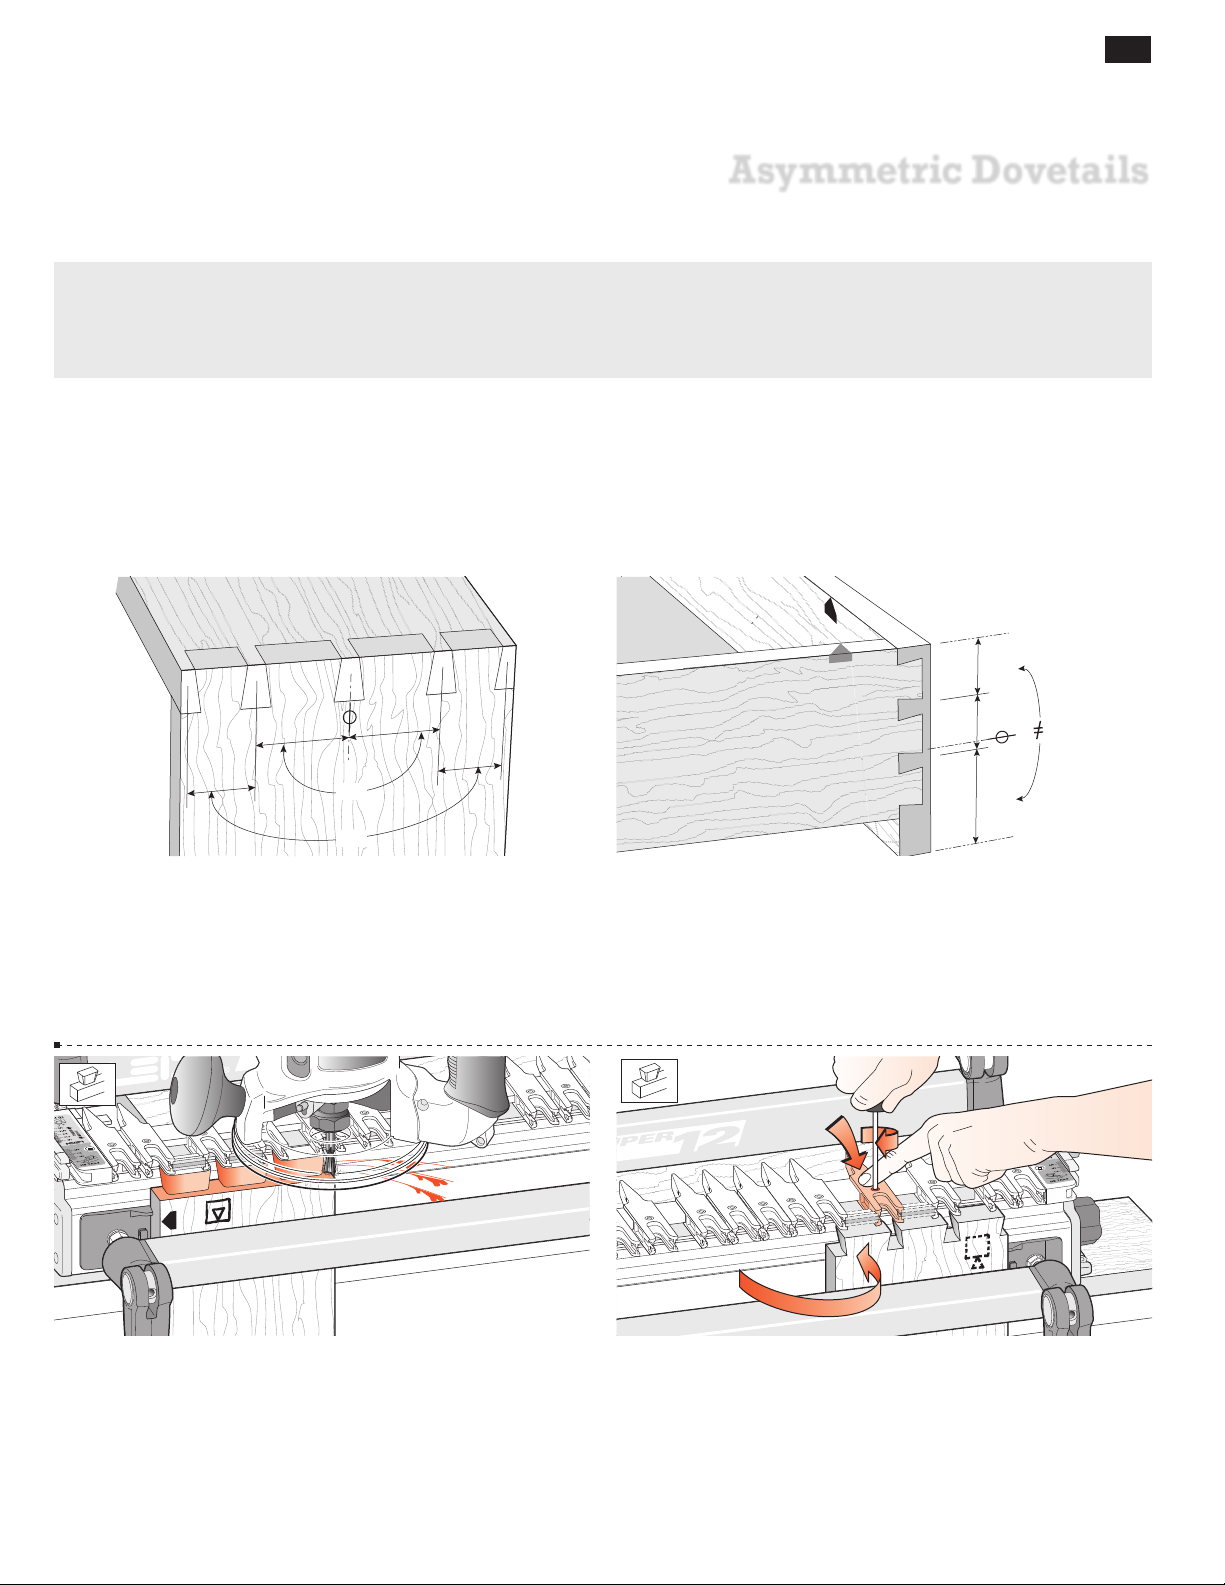
SUPERJIG - CHAPTER 12
Asymmetric Dovetails
For certain procedures, you will need to use both ends of the Leigh Superjig Jig. Asymmetrical joint layouts are one
example. On the Superjig, no joints will be truly symmetrical, but they can look symmetrical. Apparent symmetry
is desirable for aesthetic reasons, but is not required for strength. Be sure you have read and understood chapters
8 through 10 before attempting these procedures.
47
~=
~=
12-1 By symmetrical we mean a joint that looks or is approximately
symmetrical about its center line but is probably not, and need
not be precisely symmetrical. Using the Leigh jig, it is easy to cut
a joint that looks symmetrical; the pins will always align perfectly
with the tails cut at the same spacing. Remember, symmetry is
only required for appearance, not for joinery reasons.
12-3 Mount the right-hand drawer sides and pins on the left end
of the jig for routing, and…
12-2 An asymmetrical joint has a deliberately uneven layout of
pins and tails desired for a project design; for example, this dropfront drawer. The half-pin at the bottom of the drawer is much
wider than the top half-pin. As the top edges of the front and sides
are flush, it makes sense to use these edges against the side stops
at each end of the jig. Here's how.
12-4 Turn one tailboard (like turning a page in a book) to the
right end of the jig. Now lay out the fingers at the right end to
match the sockets already routed. Now simply rout the left front
corner (tails and pins) on the right side of the jig.
Page 54
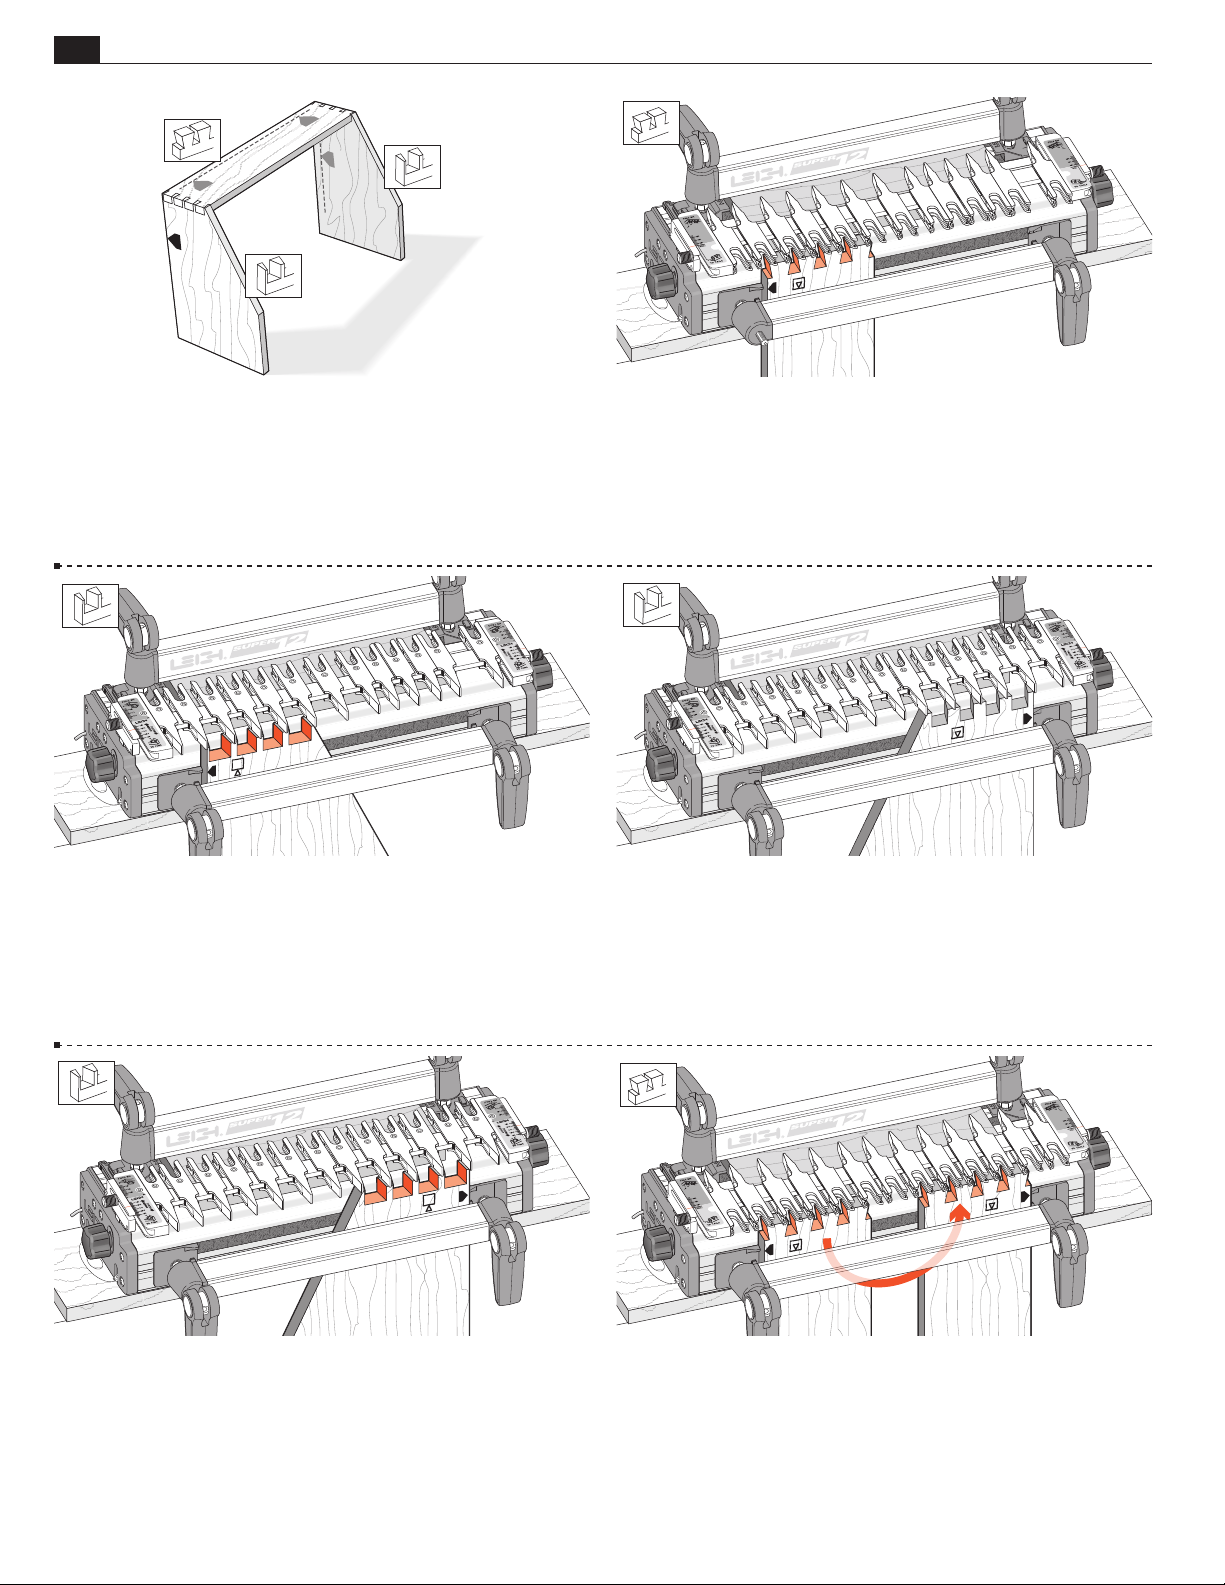
48
Chapter 12 Sup er Jig -12-18-24 User Guide
ASYMMETRIC DOVETAILS
12-5 Another example of asymmetry is the top corners of a slantfront desk. The joints themselves may be symmetrical, but they
must be routed on opposite ends of the jig because the sloped
front edges will not register accurately against the fixed vertical
side stops.
12-7 The left side of the desk goes against the left side stop e.
Rout the pins.
12-6 At the back of the desk both sides and top are flush, so the
rear edges are set against the side stops. Place the left end of the
top tail board against the left side stop e. Rout the tails.
12-8 To lay out the joint at the right end of the jig, turn the left
hand tailboard (like a book page) against the right side stop. Lay
out the fingers over the pins you just cut.
12-9 Place the right side of desk against the right side stop f.
Rout the pins.
12-10 Rotate the finger assembly to TD Tails mode. Clamp the
tailboard in the left side of the jig and rout the tails. Then rotate
the board and clamp against the right side stop to rout the tails in
the other end.
Page 55
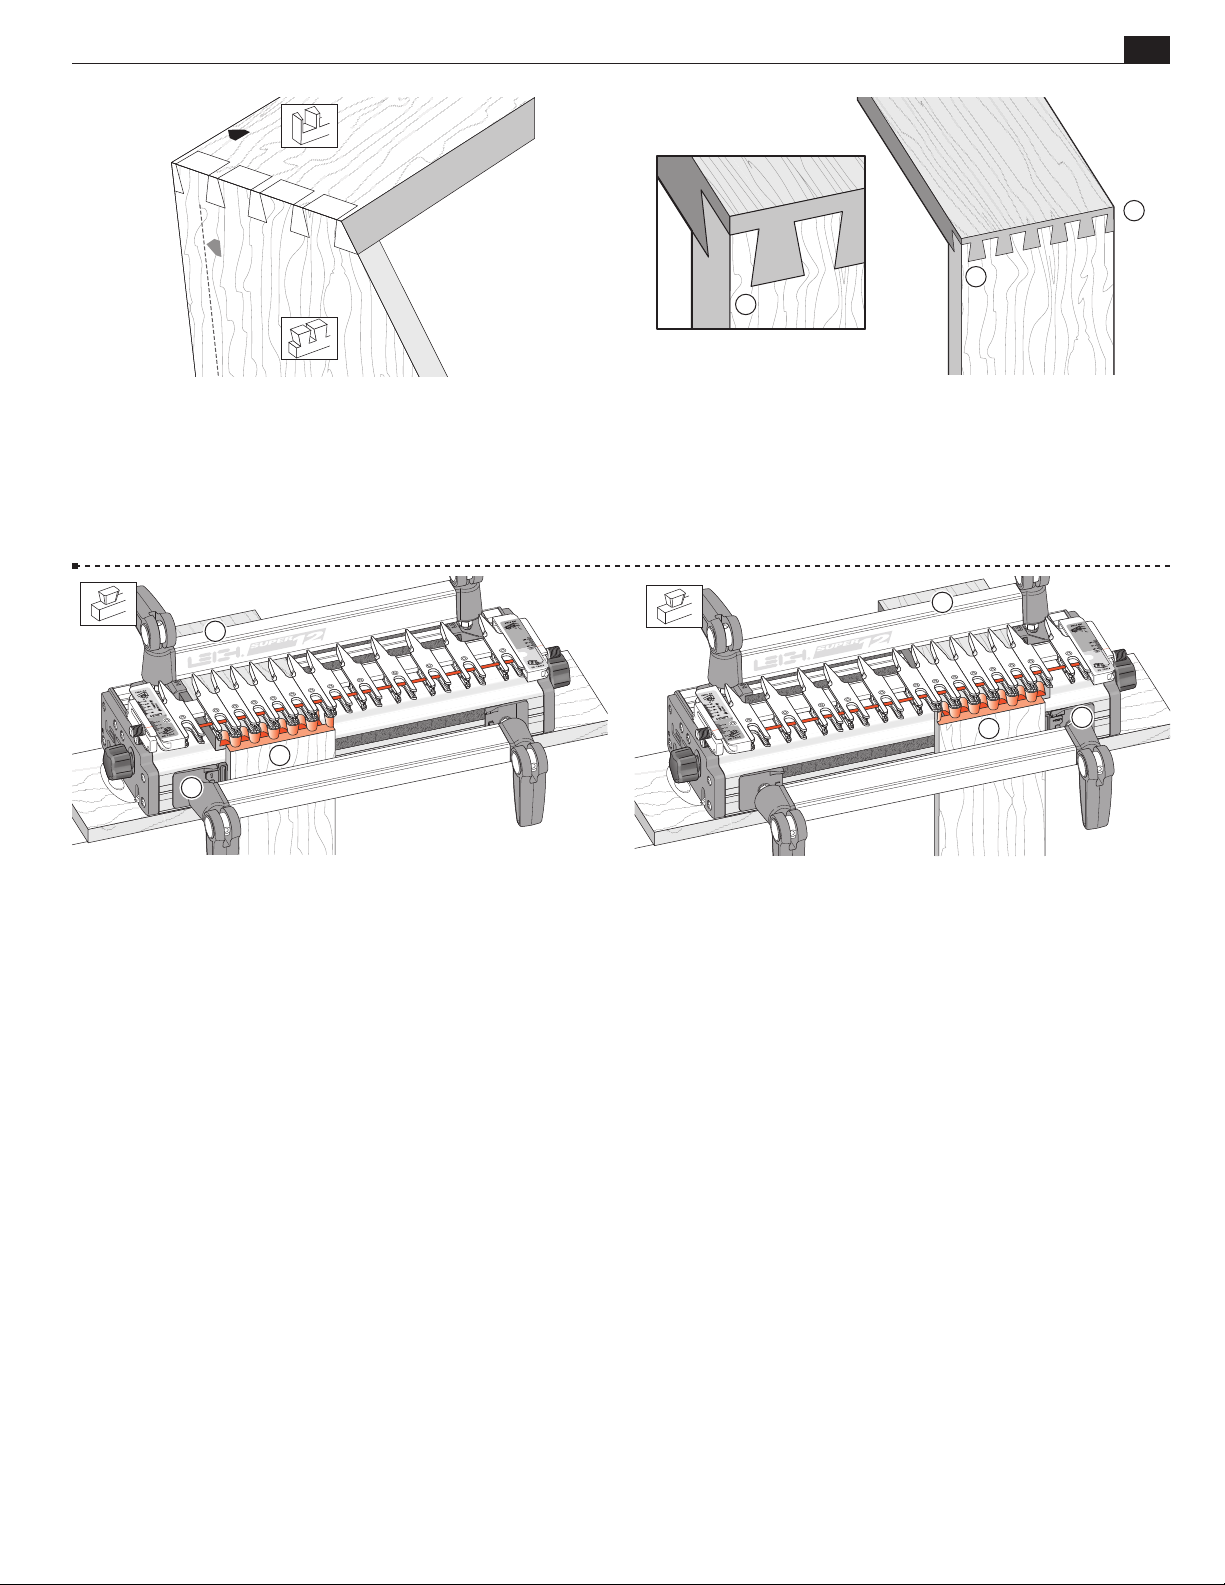
ASYMMETRIC DOVETAILS
Chapter 12Super J ig -12-18-24 User Guide
2
2
49
1
12-11 Note: If, in the slant-front desk example, the pins were in the
1
1
3
12-13 However, if this is not an option, the unattractive edge
can be hidden from view at the bottom of drawers. Simply rout
the right front and left rear drawer corners on the left side of the
jig , and then…
12-12 Asymmetric “Single Pass” Dovetails
Single pass dovetails become asymmetrical when a board width
falls between joint pitch dimensions on the board width chart,
page 40. Joint side edges will have a proper half pin on one side
and an unattractive half-tail on the other . It is preferable to
design drawer openings to suit the board width chart dimensions.
2
2
3
12-14 …the left front and right rear drawer corners on the right
side of the jig . The Spacer is used to offset the drawer sides at
both ends of the jig .
■
Page 56
50
Chapter 12 Sup er Jig -12-18-24 User Guide
ASYMMETRIC DOVETAILS
Page 57
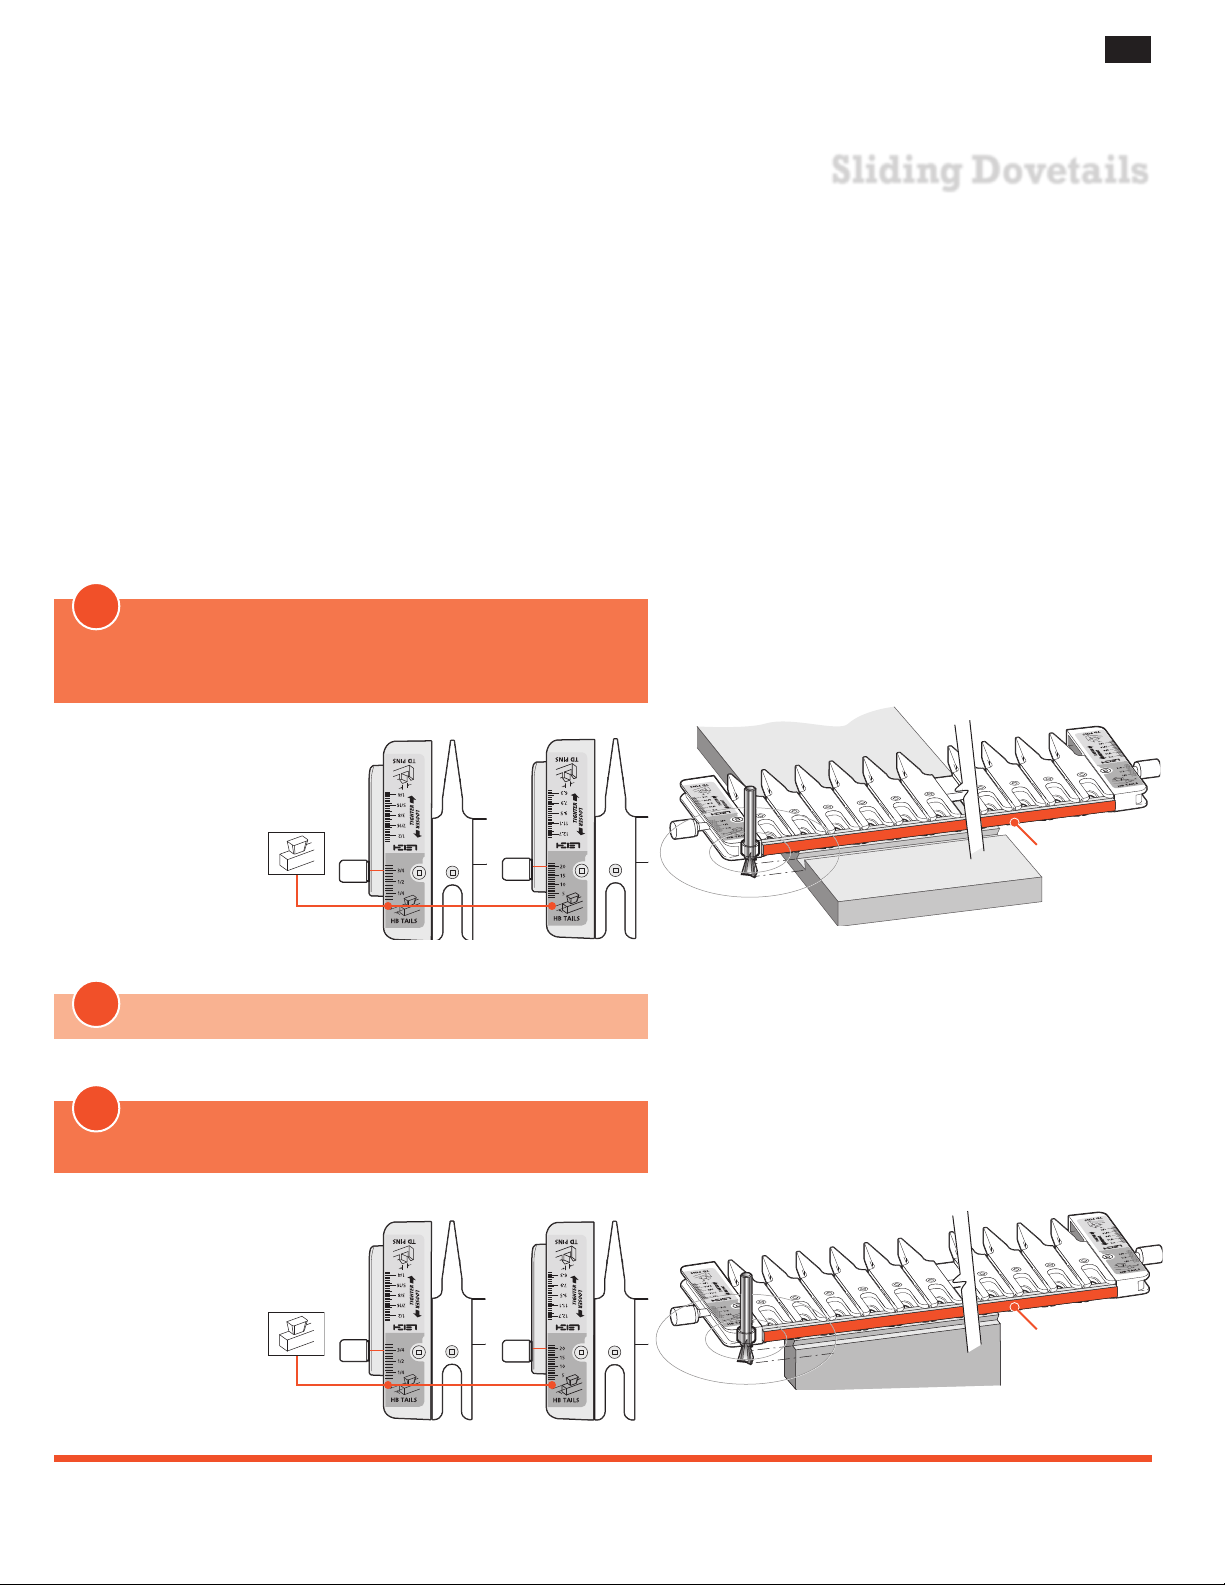
1
With the Finger Assembly in
HALF-BLIND DOVETAIL TAILS (HB TAILS) mode,
install the cross-cut fence
51
SUPERJIG - CHAPTER 13
Sliding Dovetails
Sliding Dovetail
Inches Millimetres
slots are cut
across the board
face.
2
KEEP the finger assembly in the same mode
3
Sliding Dovetail tails
are cut across the board end edge
Inches Millimetres
Active
Guide Surface
Active
Guide Surface
Page 58
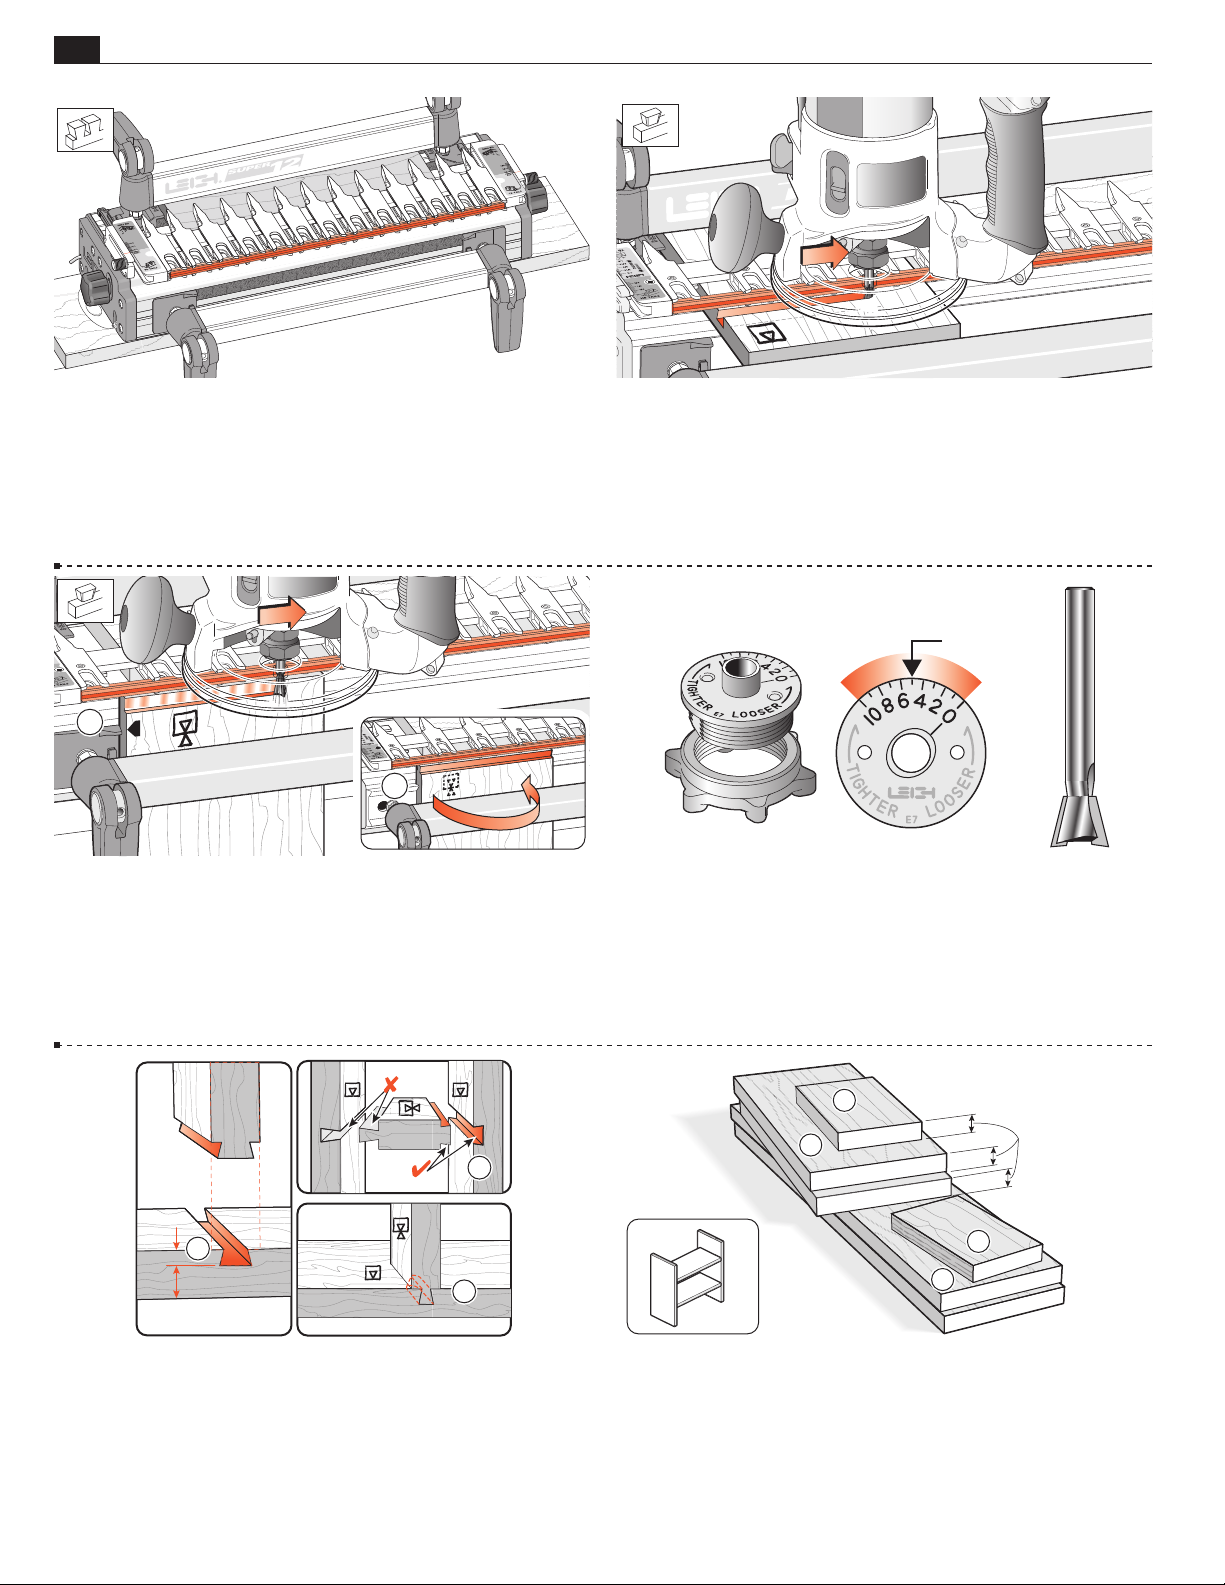
52
Chapter 13 Sup er Jig -12-18-24 User Guide
SLIDING DOVETAILS
13-1 With the finger assembly in the HHB TAILS mode, the
cross cut fence fits into the recesses in the ends of the tail guides
to allow routing of sliding dovetails.
Space the guides fairly evenly across the jig and firmly seat the
fence into end of each guidefinger to ensure a straight cut.
1
2
13-3 Across the top ends of vertical boards to cut the tails. First
rout one side ...
Then turn the board side-over-side to cut the other half of the
tail .
13-2 Using the cross cut fence as a guide surface for the guidebush,
you can make lateral router cuts across the faces of horizontal
boards (dovetail slots), and...
5
13- 4 Turn the e7‑Bush to “5” and use the No. 120-8, 1⁄2"x 14°
bit for sliding dovetails. This e7‑Bush setting will allow for fine
fit adjustment later.
7
A standard ~
⁄16"[11,1mm] guidebush (min. depth 1/4" see page
67) can be used but without the fine adjustment provided by the
e7‑Bush.
2
1/3
1
2/3
3
13-5 On a full width joint, the slot depth-of-cut should be no more than
⁄3 the board thickness . If the tail board is a load-bearing horizontal
member (e.g., bookshelf or step), make the tail fairly thick for good tail
neck strength . Shorter sliding dovetails for less structural demand
may be slightly deeper, with narrower profiles, especially if appearance
is important (e.g., where narrow rails join wider boards).
4
3
1
=
2
13- 6 Use 3⁄4"x51⁄2"[20x140mm] softwood to make two slot
boards , plus one narrow test slot board , two tail boards
and one narrow test tail board . The tail boards and test tail
board must be exactly the same thickness. This will make two
uprights and two shelves.
Page 59
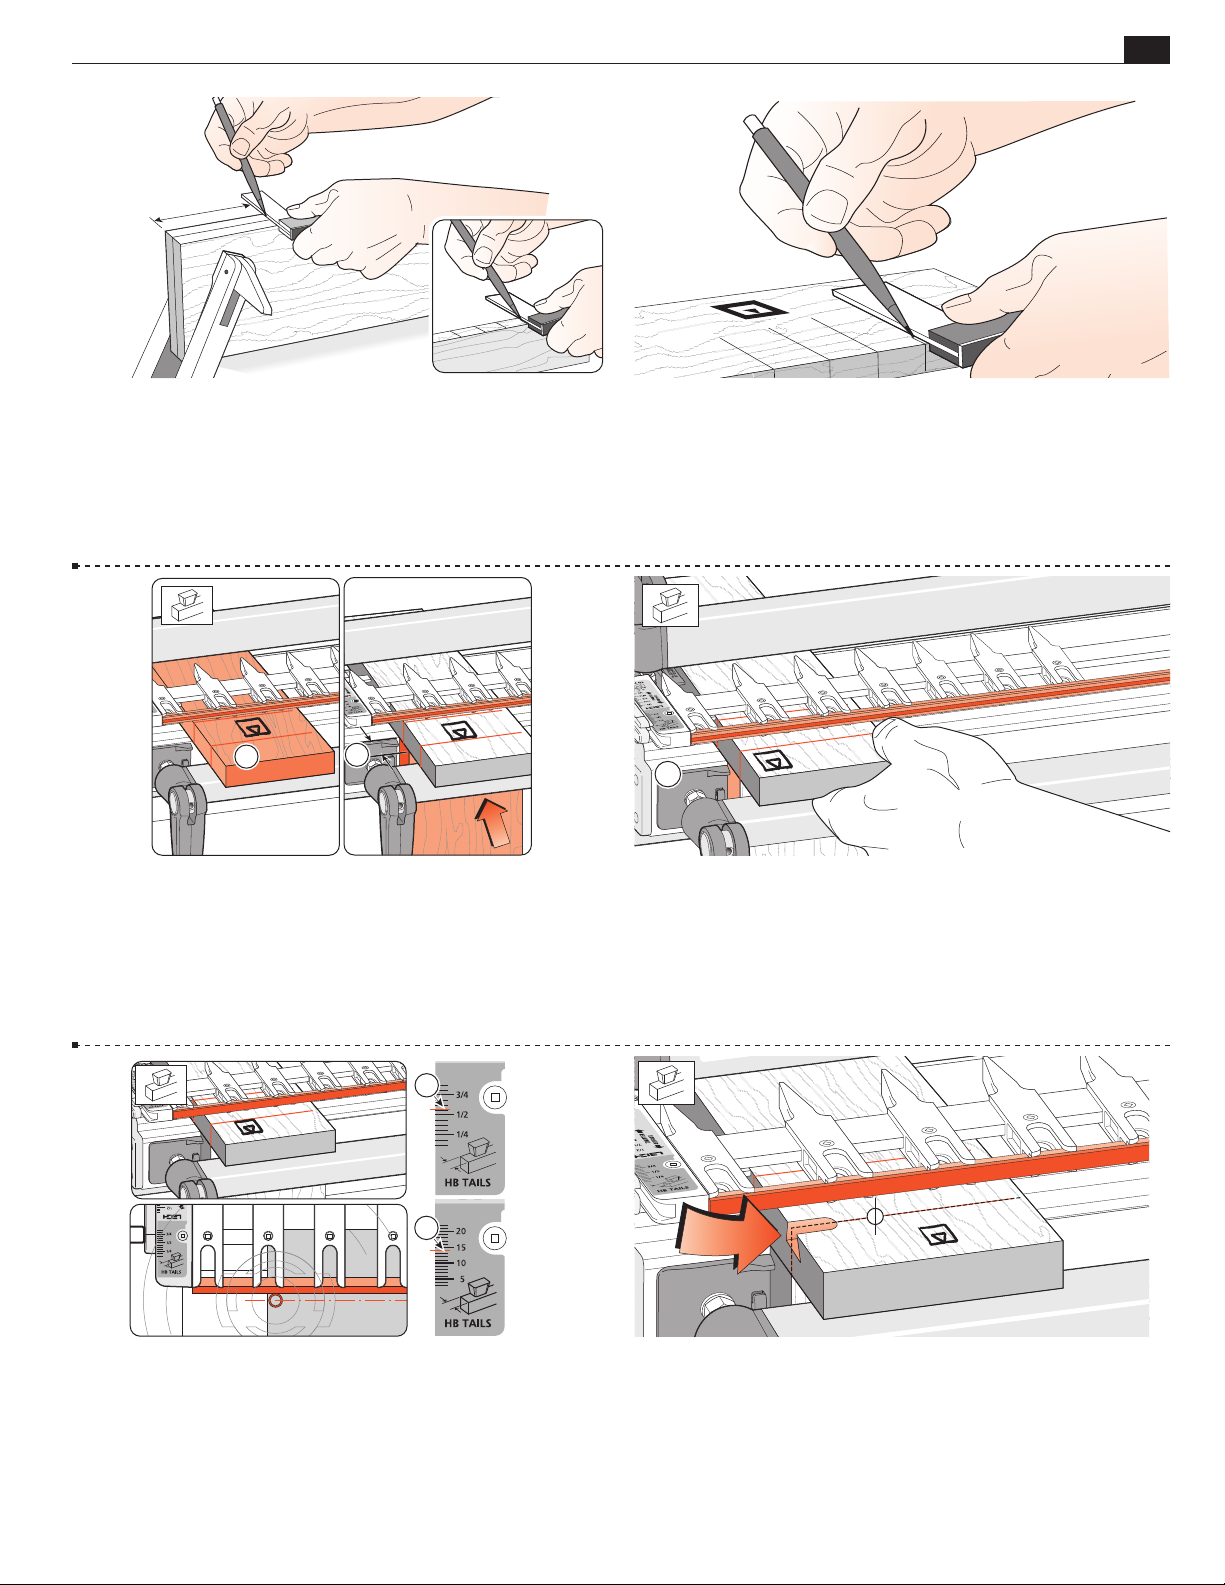
SLIDING DOVETAILS
Chapter 13Super J ig -12-18-24 User Guide
53
13-7 Marking Out: Do not mark the slot positions on the board
shelves. Stay at least 7"[180mm] in from the ends for clamping
on this test project. 13-25 describes how to rout close to both ends.
Mark the narrow test slot board in the same way at several closely
spaced random spots. This board is used only for setup.
1
2
13-9 Mount the test slot board in the rear clamp, markings up .
3
Mount a
⁄4"[20mm] thick square-ended board vertically in
the front clamp against the side stop, with the top edge butting
the underside of the test board (yes, the 3⁄4"[20mm] thickness is
13- 8 On the test slot board only, square the marks across the
face.
3
13-10 Position and clamp the test board so that one of the edge
marks is in line with the outside edge of the vertical board .
1
1
13-11 With the finger assembly (including the cross cut fence)
on the support brackets in the HHB TAILS mode, set the scale
9
⁄16"[14mm] . The routed slot will be close to centred on the
to
slot line. Make sure the finger assembly is level and sitting flush on
13-12 Adjust the bit so the cut depth is about 5⁄16"[8mm].
Rout from left to right maintaining light inward pressure of the
guidebush on the fence. Rout in only about 1"[25mm] and back
out again.
Do not lift the router.
Page 60
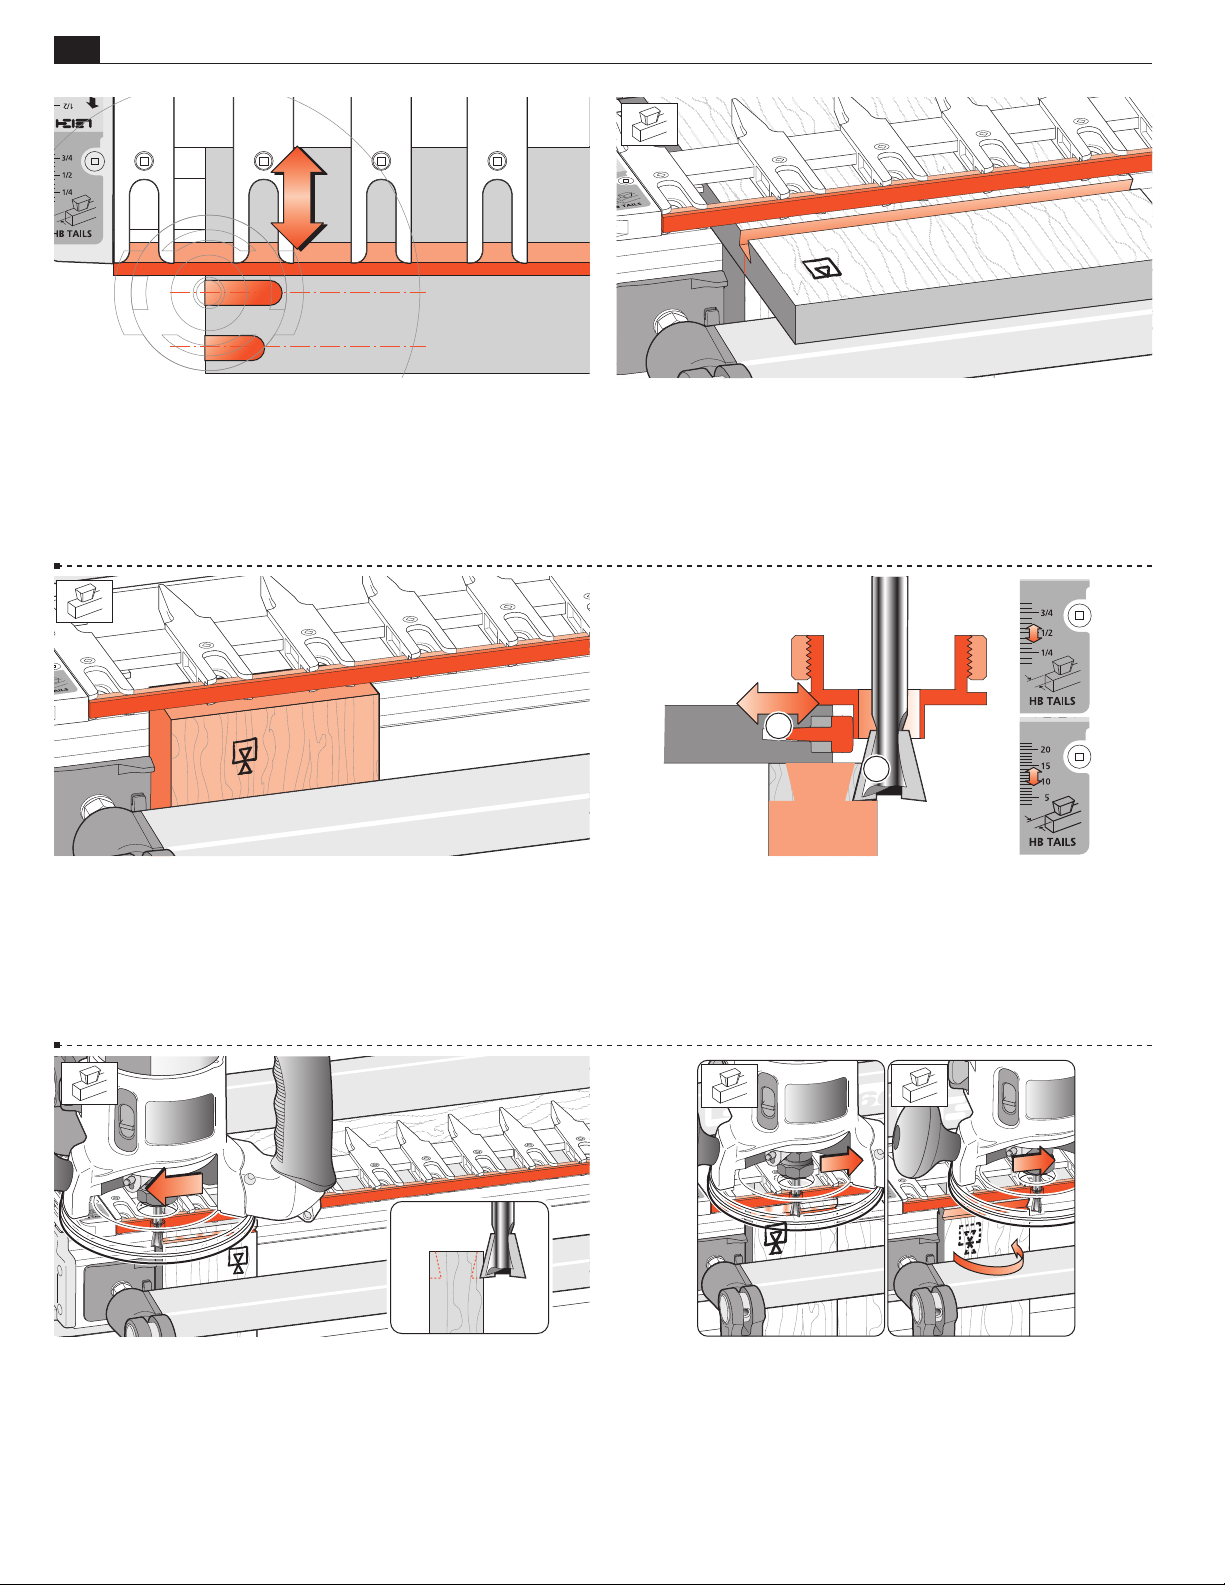
54
Chapter 13 Sup er Jig -12-18-24 User Guide
SLIDING DOVETAILS
13-13 Check to see if this short slot is centred on the pencil line.
If not, adjust the finger assembly in or out and re-test on the other
lines as necessary until the slot is centred. Lock the finger assembly
in this position and record the setting for future reference.
13-15 Replace the spacer board in the rear clamp, and with
the finger assembly on the spacer board, mount a test tail board
vertically in the front clamp, flush under the guidefingers. Either
side can face out
j
.
13-14 Now rout sliding dovetail slots in the two main slot boards
with the boards in the horizontal position in the rear clamp, slot
side, that is inside face
The guidefingers must be flush on the board.
13-16 The HHB TAILS scale is not designed for this mode,
but it does allow you to make quick adjustments for tail size and
joint fit on sliding dovetails.
Adjust and set the finger assembly so it is clear that the routed
tail will be too large for the slot.
up.
i
1
2
13-17
Make one light pass from right to left (climb
routing). Make sure you control it firmly, because it is driven in
this direction by the bit. Only the tip of the bit should be cut‑
ting on the first cut (see inset). This back or climb routing leaves
a very clean shoulder in side grain.
Rout one side of the test tail board.
13-18 Finish left to right, with the guidebush touching the fence.
Turn the test tail board around in the jig and rout the other side
in the same manner.
Page 61
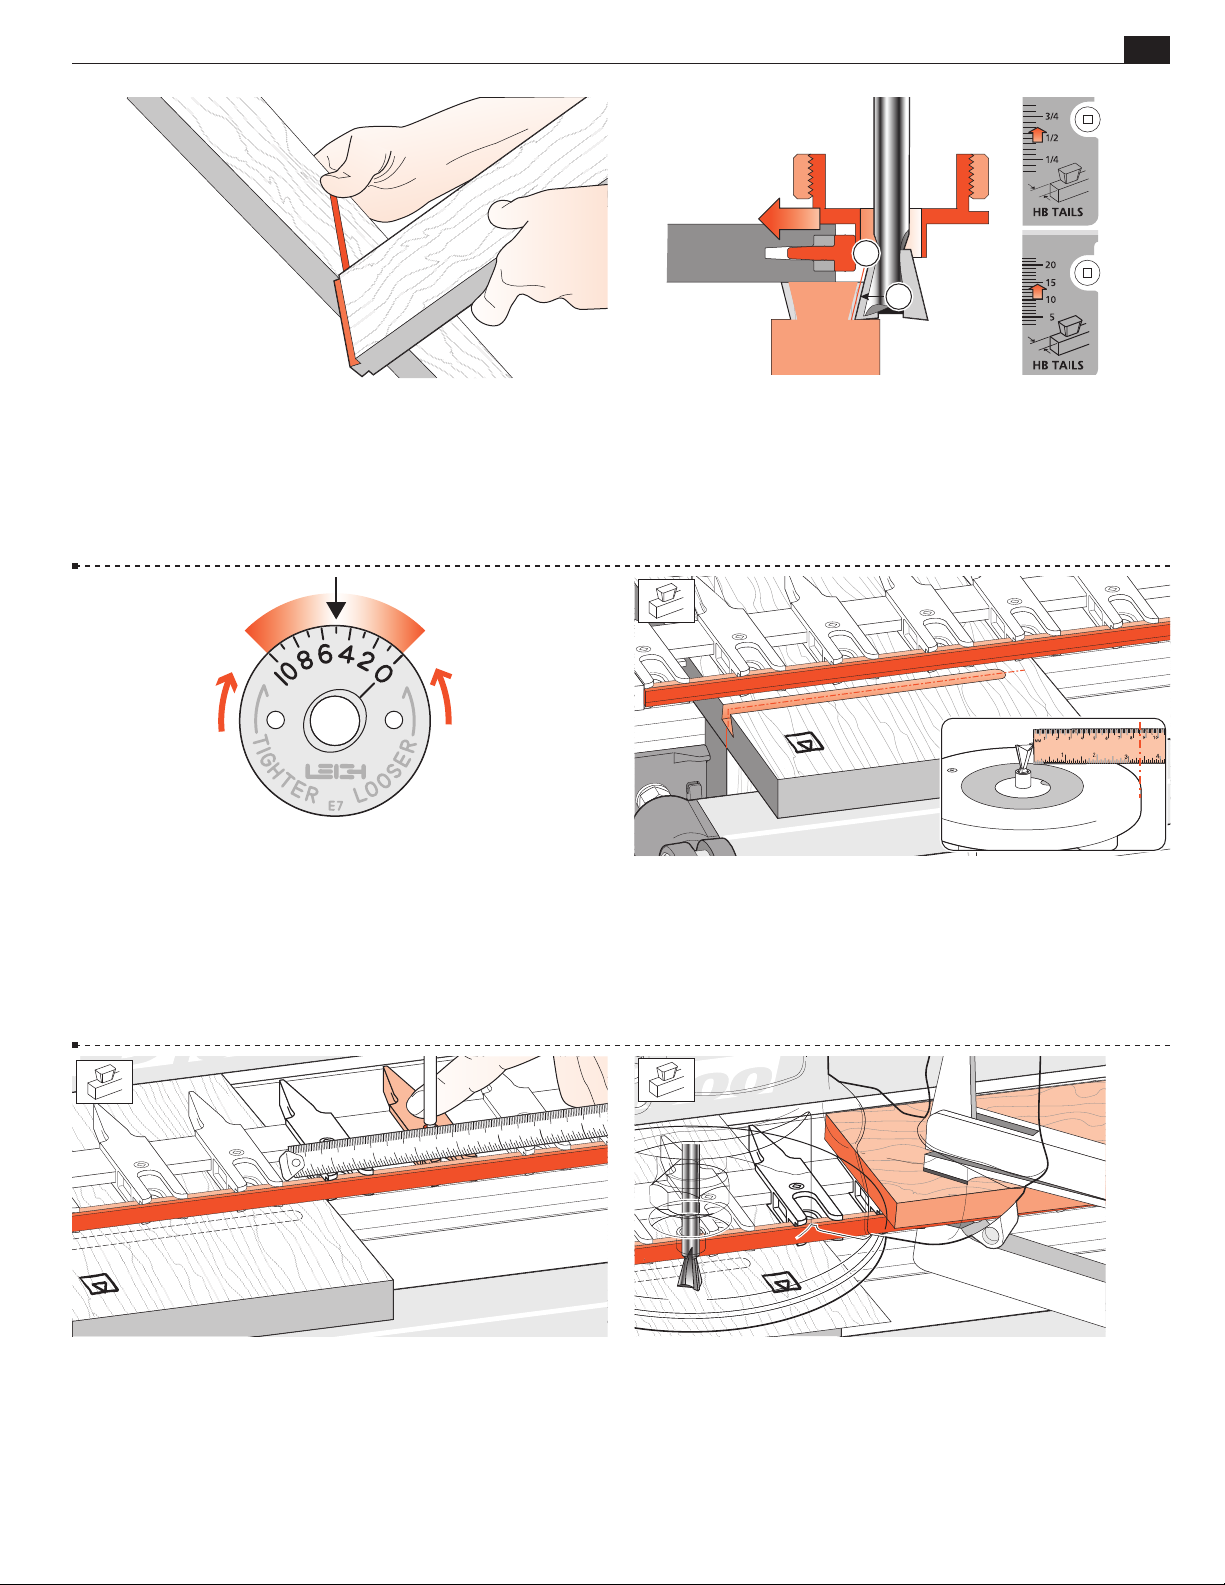
SLIDING DOVETAILS
8
100
Chapter 13Super J ig -12-18-24 User Guide
2
1
55
13-19 Test the joint for fit. The tail should be too big. If it is
too small, adjust the finger assembly outward by at least half the
difference and rout another test tail on the other end of this test
board.
L
O
O
S
E
R
T
I
G
R
E
T
H
13-21 Note: the e7‑Bush adjustment for sliding dovetails works
reverse to normal. Turn it down for tighter fit, up for looser.
Adjust the e7‑Bush for a fine fit: If fit is loose, turn the bush lower;
if fit is tight, turn it higher. When the fit is satisfactory, rout one
end of a project tail board and test again. If the fit is good, rout
all the other ends.
13-20 If the tail is too wide move the finger assembly in
toward the jig by half the amount the tail is too wide . Rout the
same test board again. Adjust and re-test until fit is slightly loose
or slightly tight.
13-22 Stopped Sliding Dovetails
If a stopped sliding dovetail is called for...
Measure from the outside tip of the dovetail bit to the edge of
the router base.
90
80
70
60
50
40
30
20
10
100
60
50
40
30
20
10
1 2 3 4
90
80
70
5
13-23 Measure the same distance from where you want the slot
7
6
stopped to a position on the finger assembly. Move a guidefinger
to that point and mark the guidefinger with a felt pen as a visual
router stop mark…
13-24 Or lightly clamp (with a soft‑jawed clamp) a short board
to the finger assembly to act as a router stop.
Page 62
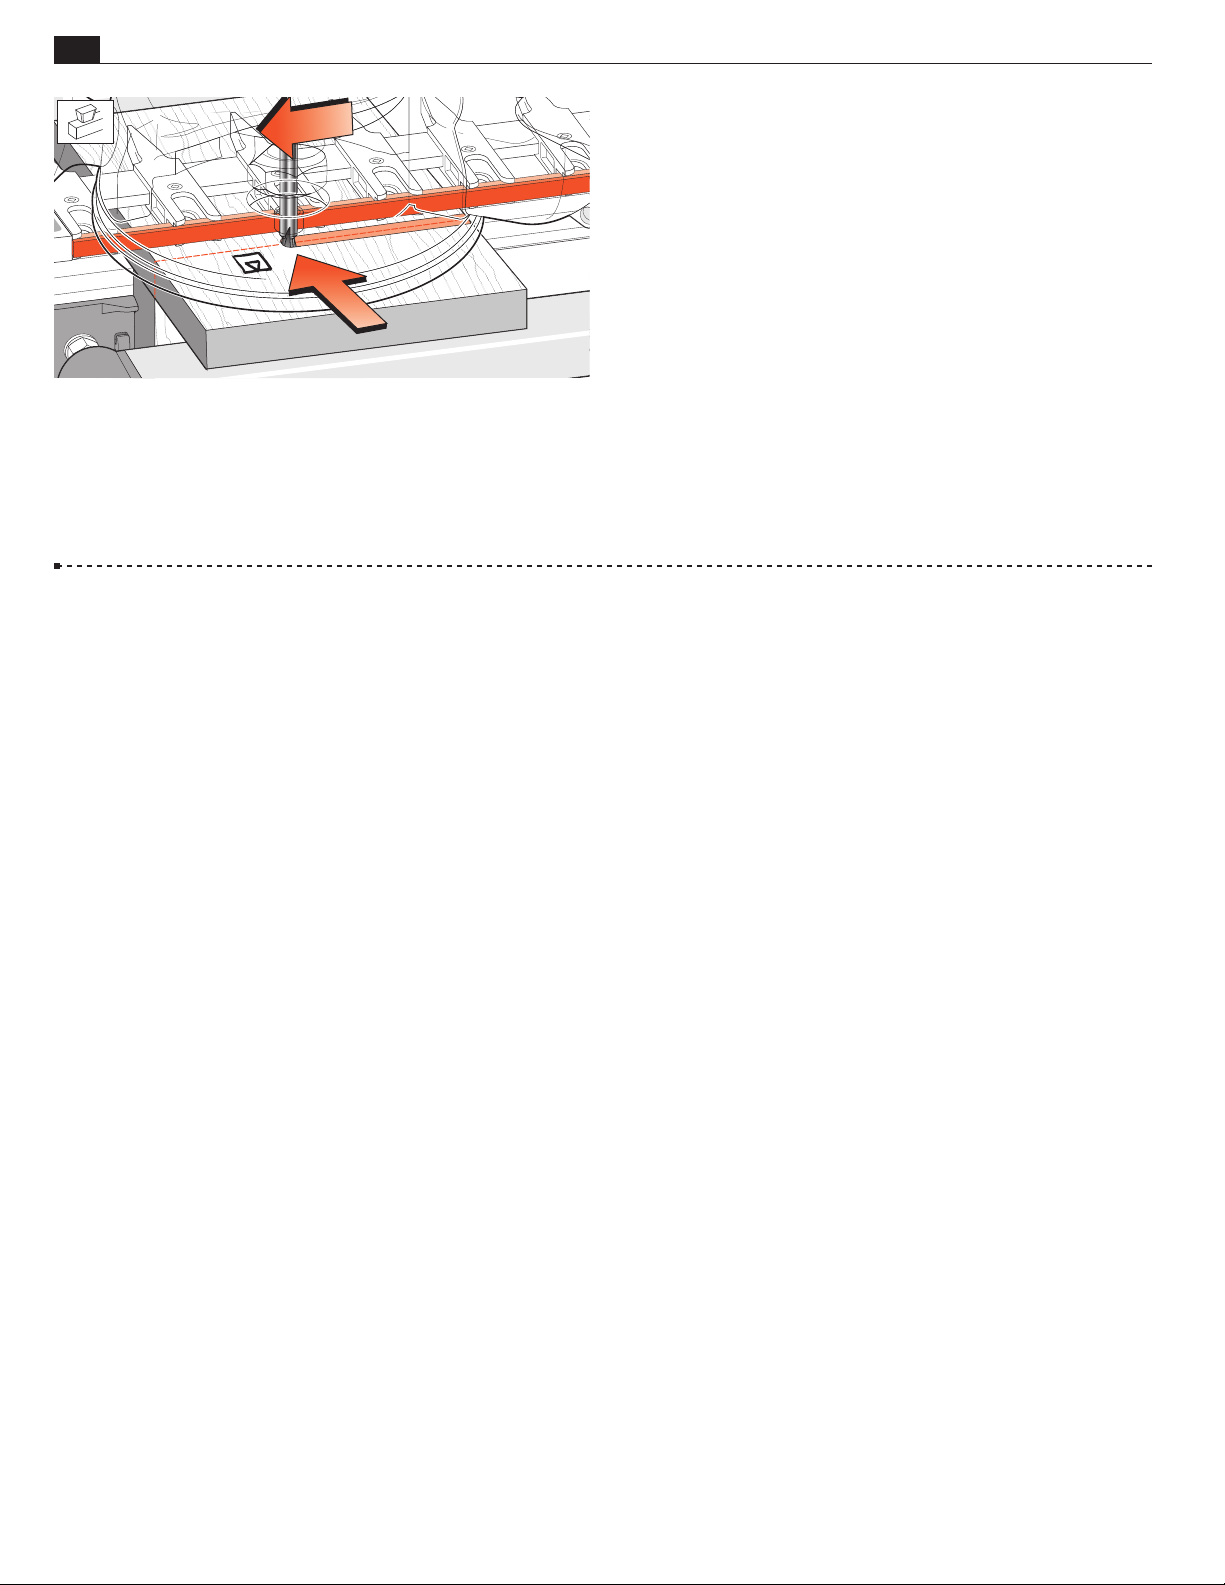
56
Chapter 13 Sup er Jig -12-18-24 User Guide
SLIDING DOVETAILS
13-25
because the bit’s clockwise rotation pulls the guidebush
against the fence. However; as when routing close to both ends of a
board, it may be necessary to rout slots from right to left. Bit rotation
will tend to pull the router away from the fence. Feed slower and
maintain constant guidebush pressure against the fence.
Dovetail slots preferably are routed from left to right
■
Page 63
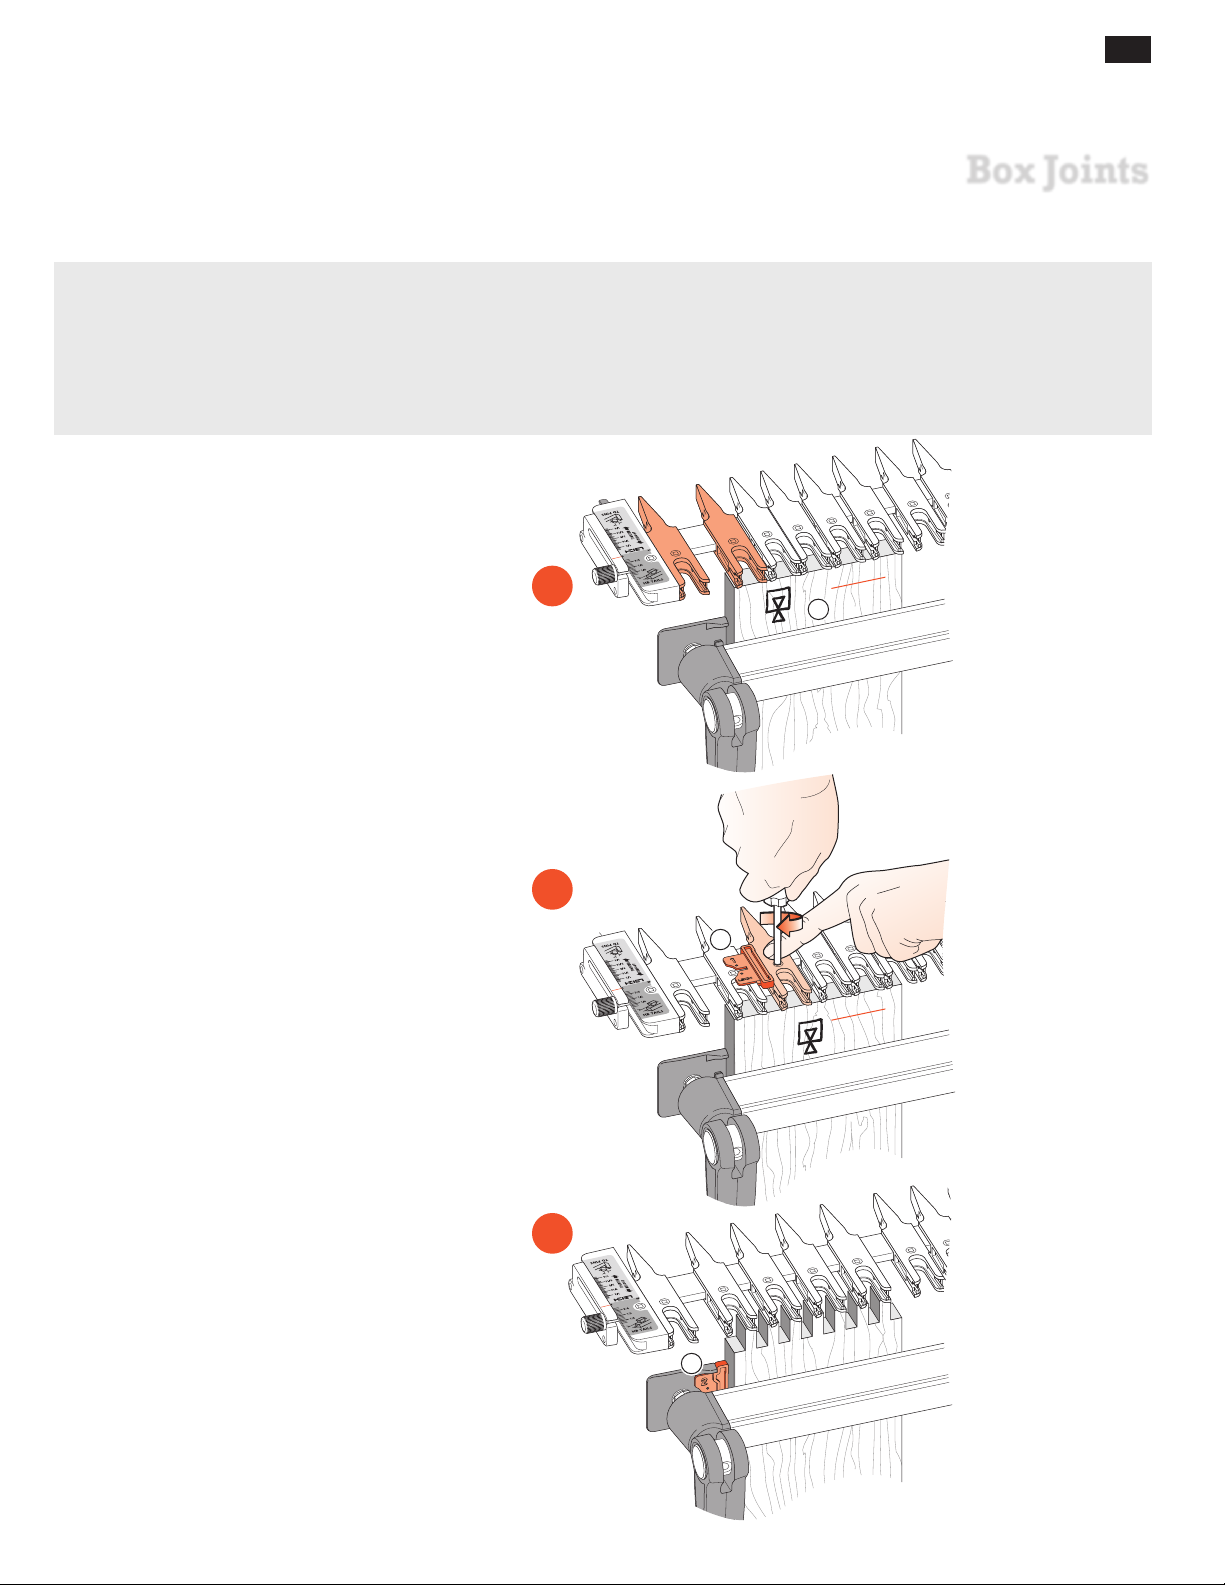
SUPERJIG - CHAPTER 14
Box Joints
Actual Joint Sizes
The Superjig finger assembly was originally designed solely for dovetailing. Adapting the assembly for box jointing
was a serendipitous combination of luck (existing guides approximately the correct dimension) and clever design;
the e7‑Bush and Spacer.
5
So the nominal
respectively.
Concept of Operation
The first board is set against the side stop ➀.
⁄16" and 5⁄8"[8 and 16 mm] box joint sizes are actually 21⁄64" and 21⁄32" [8,3 and 16,7mm]
1
1
57
The Spacer is used to space the guide fingers ➁.
The Spacer is also used on the side stop ➂ to accurately offset mating work pieces for correct board to
board joint alignment.
2
2
3
3
Page 64
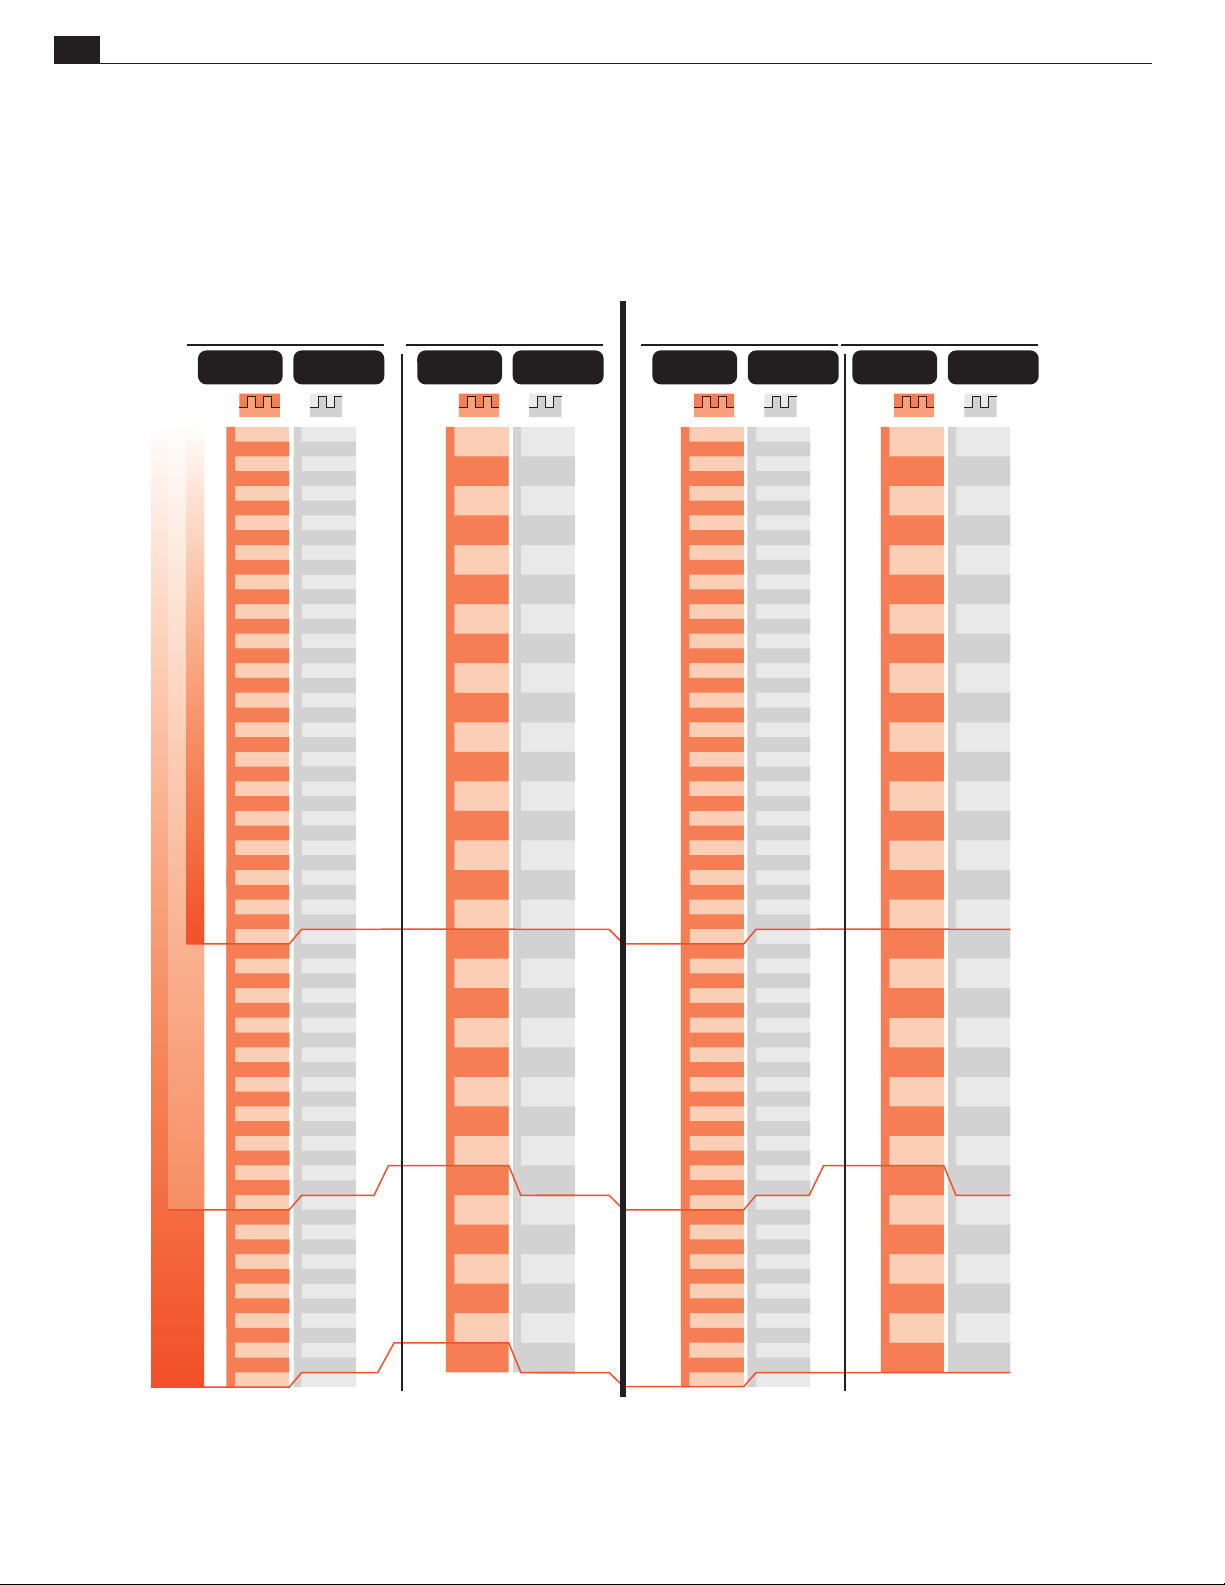
58
SuperJig 24
Chapter 14 Sup er Jig -12-18-24 User Guide
Choose your Board Width:
Symmetrical joints: Use the red column
Asymmetrical joints: Use the grey column
Count the total sockets and pins in the first (white) column
BOX JOINTS
Board Width - INCHES
Board Width - MILLIMETERS
5/16" 5/8" 8mm 16mm
Symmetrical Symmetrical Asymmetrical Symmetrical Asymmetrical SymmetricalAsymmetrical Asymmetrical
1
2
3
4
5
6
7
8
9
10
11
12
13
14
15
16
17
18
19
20
21
22
23
24
25
26
27
28
29
30
31
32
33
34
SuperJig 12
35
36
37
38
39
40
41
42
43
44
45
46
47
48
49
50
51
SuperJig 18
52
53
54
55
56
57
58
59
60
61
62
63
64
65
29/
1 9/
2 7/
2 7/
3 17/
4 3/
4 27/
5 1/
6 5/
6 13/
7 15/
8 1/
8 25/
9 13/
10 1/
10
11 3/
12 5/
12 13/
13 15/
14 1/
14 25/
15 7/
16 3/
16 3/
17 13/
18 1/
18 11/
19 11/
20
20
21 5/
1
32
1
/
4
1
16
1 29/
32
8
32
16
32
2
32
16
32
8
32
32
16
23
/
8
32
8
16
32
4
16
21
/
16
32
2 9/
16
3 7/
32
3 7/
8
4 1/
2
5 5/
32
5 13/
16
6 15/
32
7 1/
8
7 25/
32
8 7/
16
9 3/
32
9 3/
4
10 13/
11 1/
11 27/
12 1/
13 5/
13 25/
14 7/
15 3/
15 3/
16 13/
17 1/
17 23/
18 3/
19 1/
19 11/
20 11/
21
32
16
32
2
32
32
16
32
4
32
16
32
8
32
16
32
32
16
32
32
32
16
32
32
2
29
3
1
/
32
4
7
5
3
/
6
1
7
4
8
13
9
5
10
1
11
7
/
12
7
13
8
/
14
3
15
9
/
16
1
17
11
18
1
19
12
20
25
21
13
22
3
23
15
24
13
25
16
26
23
27
17
28
1
29
19
30
11
31
20
32
9
2
/
16
32
7
3
/
8
/
2
5
5
/
32
/
16
15
6
/
32
8
25
7
/
32
16
3
9
/
32
4
13
10
/
32
/
16
27
11
/
32
/
2
5
13
/
32
/
32
7
14
/
16
/
32
3
15
/
4
/
32
1
17
/
16
/
32
3
18
/
8
/
32
11
19
/
16
/
32
21
1
2
3
23
4
5
40
6
7
56
8
9
73
10
11
90
12
13
106
14
15
123
16
17
140
18
19
156
20
21
173
22
23
190
24
25
206
26
27
223
28
29
239
30
31
256
32
33
272
34
35
289
36
37
309
38
39
325
40
41
342
42
43
359
44
45
375
46
47
392
48
49
409
50
51
425
52
53
442
54
55
459
56
57
475
58
59
491
60
61
508
62
63
525
64
65
541
32
48
65
82
98
114
131
148
164
181
198
214
231
248
264
281
301
318
334
350
367
383
400
417
433
450
467
483
500
517
533
1
2
3
48
4
5
82
6
7
114
8
9
148
10
11
181
12
13
214
14
15
248
16
17
281
18
19
318
20
21
350
22
23
383
24
25
417
26
27
450
28
29
483
30
31
517
32
65
98
131
164
198
231
264
301
334
367
400
433
467
500
533
Page 65
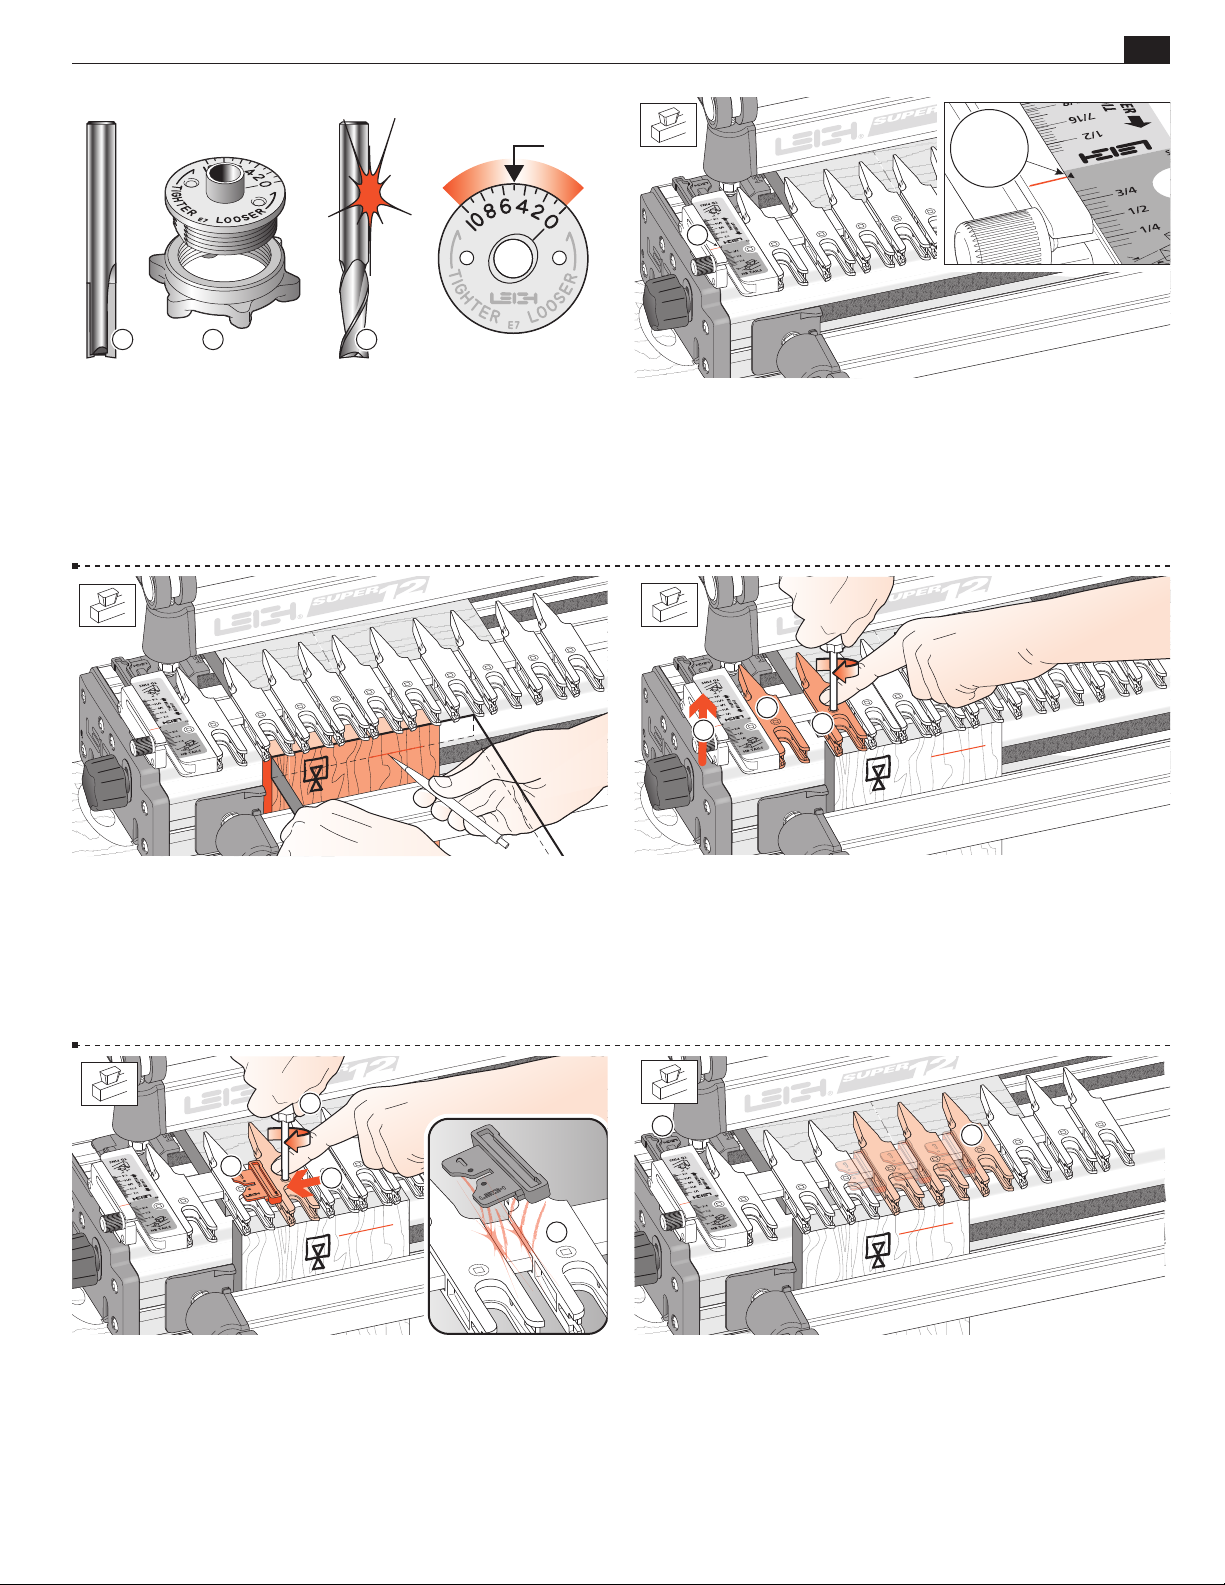
BOX JOINTS
Chapter 14Supe r Ji g-12-18-24 User Guide
59
5
1 21
14-1 Bit and Guidebush selection Only the e7‑Bush and
5
⁄16" bit that came with Superjig ➀ are required for all Superjig
box joints. Note: Spiral upcut router bits ➁ will cut cleaner than
straight flute. Where metric size bits are available an 8mm straight
5
or spiral bit may be substituted for the
⁄16". Always start test rout-
ing with the e7‑Bush set on “5”, the adjustment mid-range.
1
1
14-2 5⁄16"[8mm] Box Joints.
Place the finger assembly on the support brackets in the HB TAILS
mode, set the scales on the small triangular arrow
the assembly onto the spacer board.
3
1
2
➀ and lower
14-3 Clamp a test board in the front left clamp, against the side
stop with the top edge flush under the guidefingers. The board
may be clamped face side in or out
. Mark and adjust the depth
j
of cut to suit the thickness of the mating boards ➀.
3
1
2
4
14-5 Place the Spacer on the finger bar to the right of the second
finger, numeral 1 on top overlapping the locked finger ➀. Move the
next finger in to touch the Spacer ➁. Hold the guidefinger firmly
against the Spacer and tighten the second finger screw ➂.
As you remove the Spacer you should feel some friction; this
indicates that the guidefinger is correctly spaced ➃.
14-4 Raise the finger assembly about 1⁄16"[2mm] to allow ease
of guide finger adjustment ➀. Position the second guidefinger
1
⁄32"[1,0mm] in from the board edge ➁ and tighten the finger. The
first finger stays against the scale block as a router support ➂.
Note: Square ended boards are essential to achieve flush joint alignment.
2
1
14-6 Repeat this procedure across the jig until there is at least
one guidefinger spaced past the right side of the work piece ➀.
Tighten the unused guides. Store the Spacer on the outside of a
rear side stop ➁.
Page 66
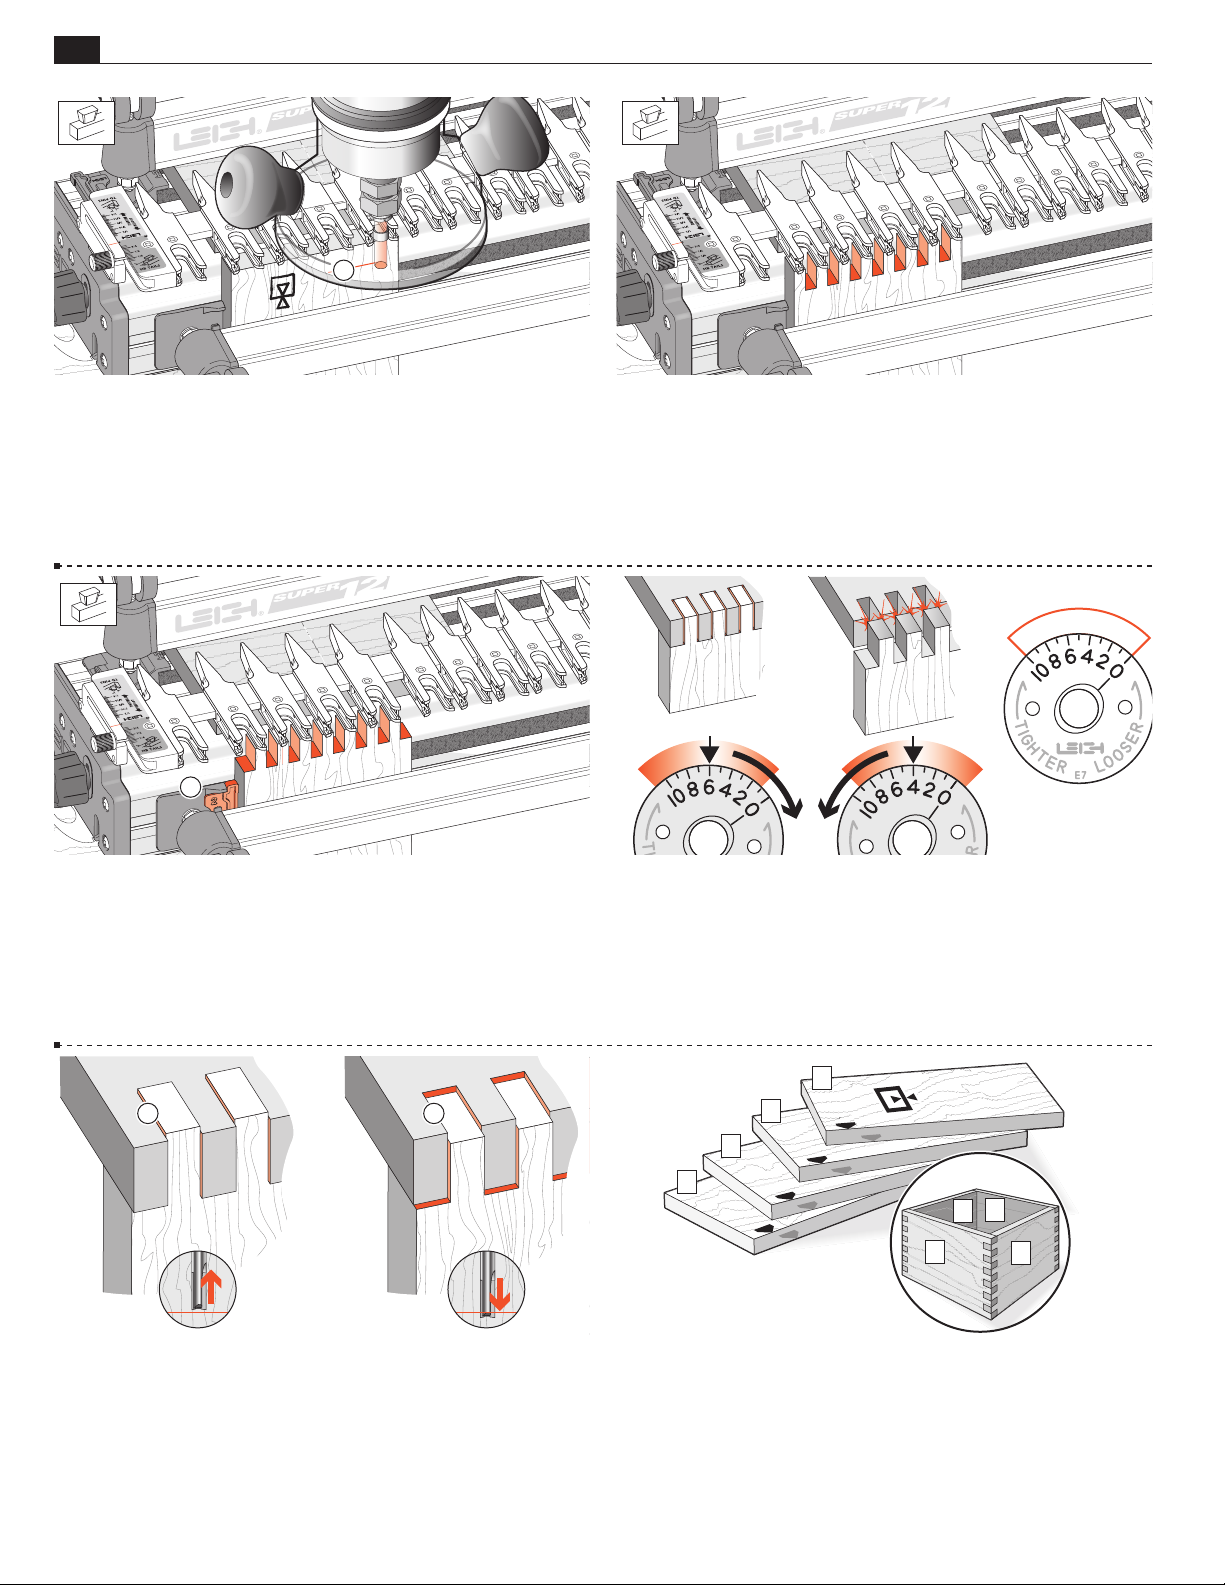
60
Chapter 14 Sup er Jig -12-18-24 User Guide
1
BOX JOINTS
14-7 Lower the finger assembly onto the spacer board and doublecheck that the bit depth is down to the center of the pencil line ➀.
Make sure the collet does not rub on the guidebush.
1
14-9 Remove the board and fit the Spacer to the front side stop
with the number 2 showing ➀. Make sure it is fully home.
Clamp the second test board with its side edge against the Spacer
and its top edge touching the guidefingers. Rout this board.
Note: Square ended boards are essential to achieve flush joint alignment.
14-8 Rout one end of the scrap board. Rout into each finger
opening and between each finger. Make sure to run the guidebush
on both sides of each opening.
14 -10 Test the two boards for fit and flushness. If the joint is
loose, turn the e7‑Bush to a higher number, say “6” and rout two
more board ends. If the joint is too tight, turn the e7‑Bush to a
lower number, say “4”. Trial and error establish the best e7‑Bush
setting and record this in the space provided here, and/or on the
pull‑out. Next time this setting will get a good first-time result
1 2
14 -11 If the joint is over-flush ➀, raise the bit slightly. If it is
under-flush ➁, lower the bit.
4
3
2
1
3
2
1
14-12 Let’s make a box.
Prepare four boards and number them 1 to 4. Then select the grain
alignment and mark the common top (or bottom) edge. Don’t
worry about face side selection; this can be done after routing.
4
Page 67
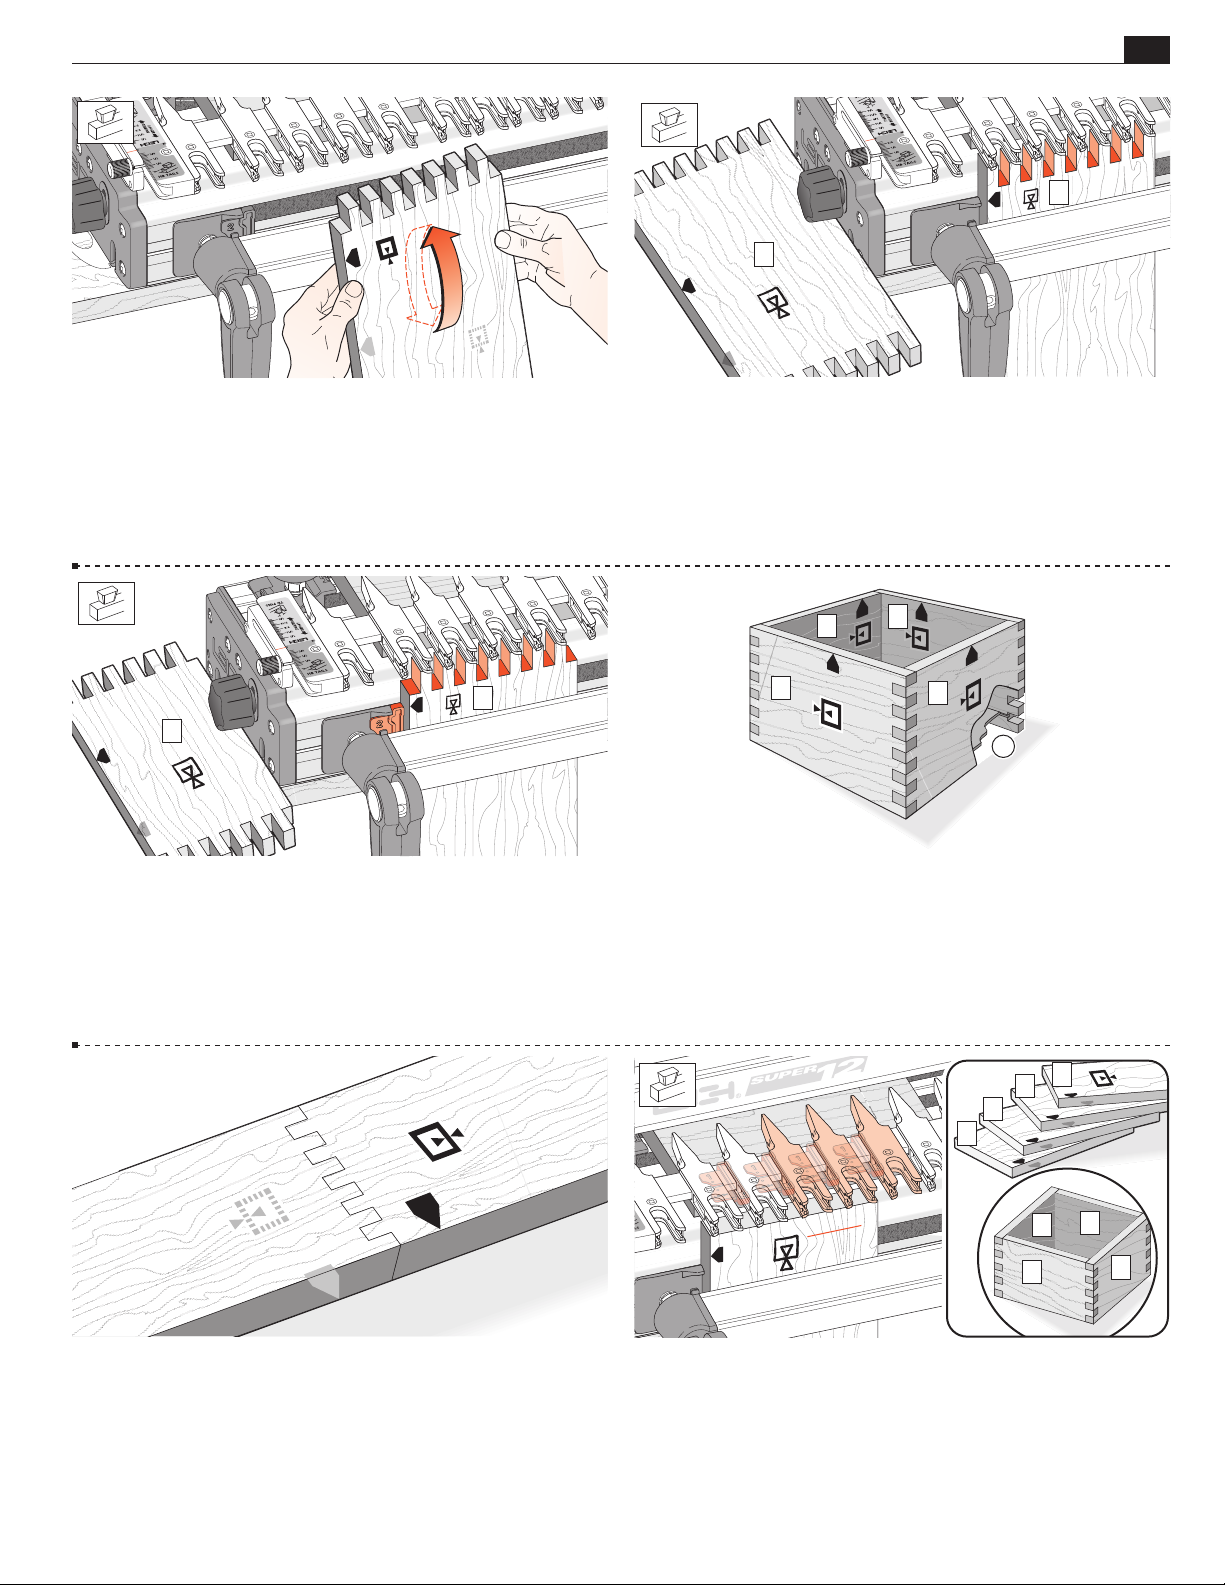
BOX JOINTS
1
Chapter 14Supe r Ji g-12-18-24 User Guide
61
3
14 -13 All box joint boards are clamped alternating face side in
and face side out [icon] always with the same side edge against
the side stop (or Spacer).
4
2
14 -15 Rout both ends of boards 2 and 4 with their edges against
the Spacer and the Spacer in the No.2 position.
Keep the same edges to the Spacer.
14-14 Rout both ends of boards 1 and 3 with their edges against
the side stop. Be sure to keep the same edge to the stop.
2
1
3
4
5
14 -16 Keeping the marked side stop edges of all boards toward the
top (or all to the bottom) of the box, select the preferred outside
faces before routing the grooves ➄ for the bottom.
4
3
2
1
4
3
2
14 -17 The same method will produce end-on-end joints. 14-18 5⁄8"[16mm] Box Joints Set up and space the guide
5
fingers exactly as for
setting. See 14-4 thru 14-10.
Prepare four boards using the board width chart for
joints and number them 1 to 4
mon edges marked.
⁄16"[8mm] joints. Start with the same e7‑Bush
around the box ➀ with the com-
1
5
⁄8"[16mm]
Page 68
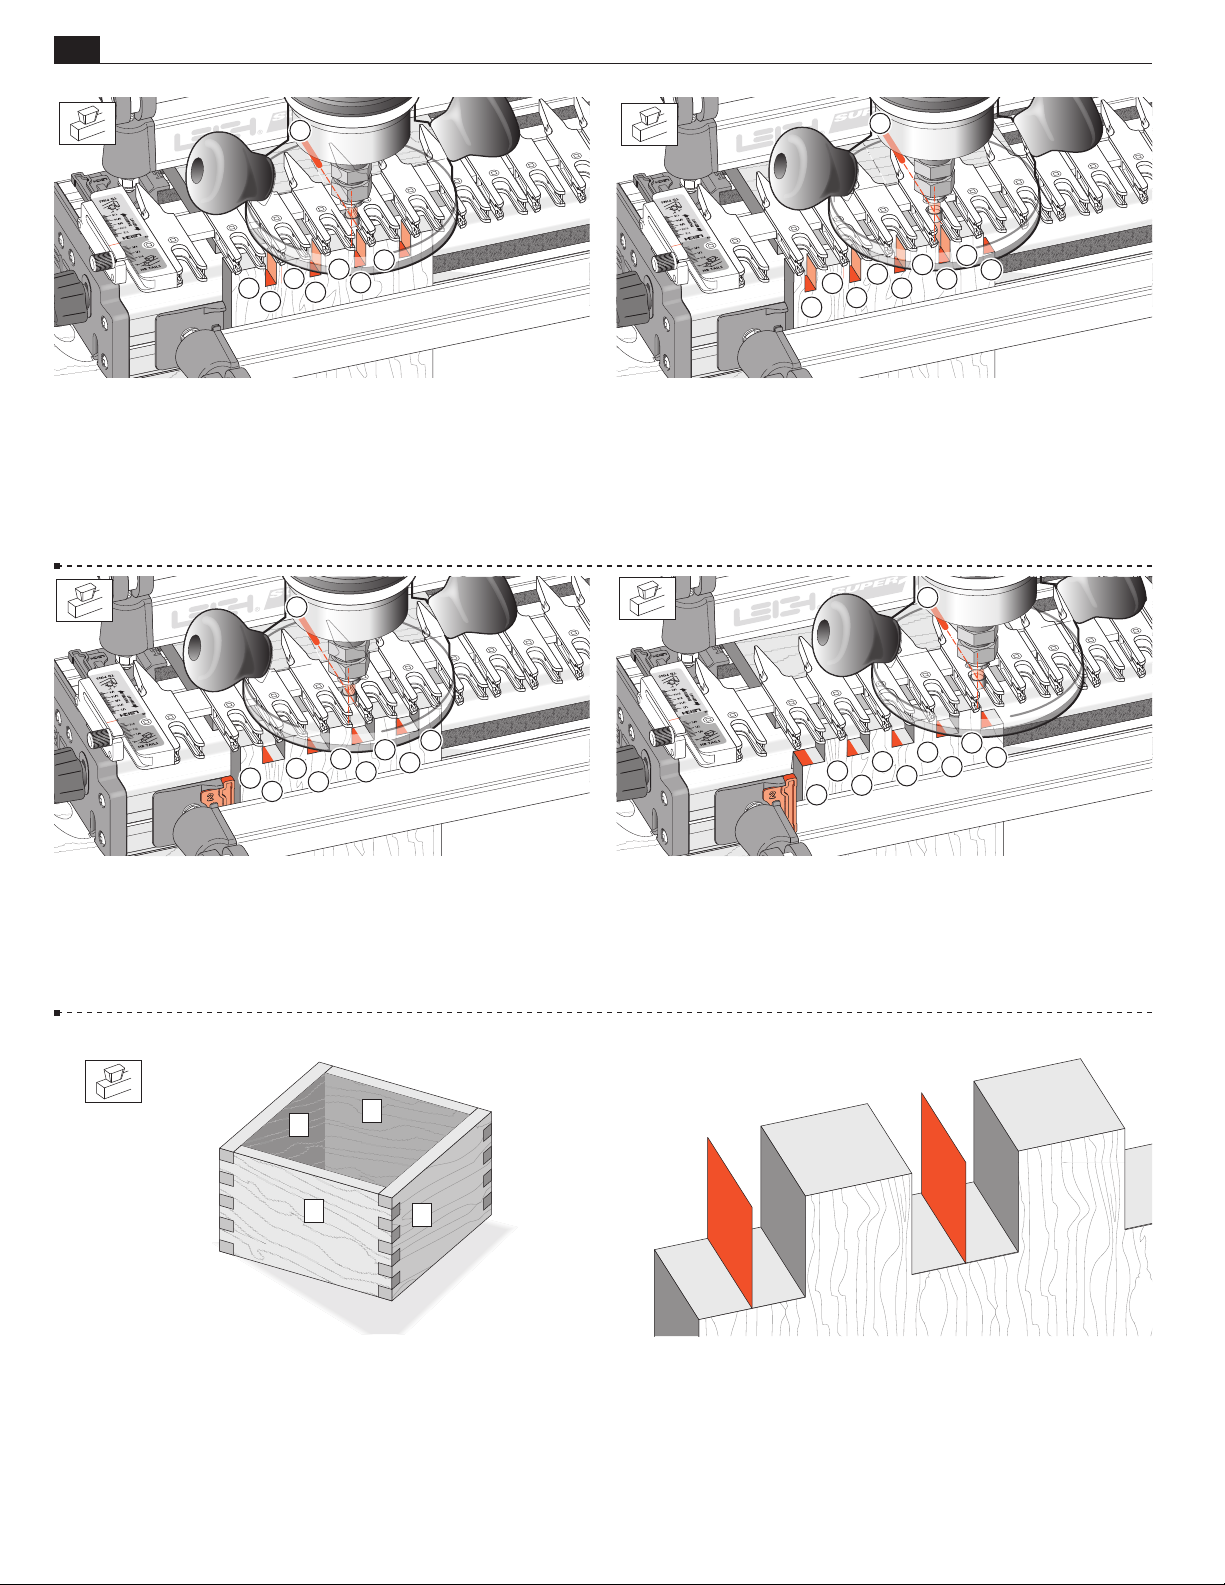
62
Chapter 14 Sup er Jig -12-18-24 User Guide
BOX JOINTS
3
2
2
2
2
1
1
1
14 -19 Rout both ends of boards 1 and 3 but only rout between
the guide finger sides ➀ not between the finger openings ➁.
Keep the common edge against the side stop
Mark the router base at the 12 o’clock position ➂ and steer
Hint:
this mark between the pointed ends of the fingers at the rear of
the assembly.
3
3
2
2
1
1
1
2
2
1
1
14-20 Now rout both ends of boards 2 and 4, with the common
edge against the side stop but only rout between the finger open‑
➀ not between the finger sides ➁.
ings
Hint: Now steer the base 12 o’clock mark along the finger
➂.
points
3
2
1
1
2
2
1
1
2
2
14-21 Fit the Spacer to the side stop with number 2 showing.
Now rout both ends of boards 1 and 3 again, with the common
edge against the Spacer and again …only rout between the guide
finger sides
➀, not between the finger openings ➁, steering the
router mark between the finger points ➂.
2
4
1
3
2
2
1
1
1
2
2
1
1
14-22 With the Spacer still in position rout both ends of boards
2 and 4, with the common edge against the Spacer and again, only
rout between the finger openings
➀, steering the router mark
along the finger points ➂.
14-23 Joint fit Check for joint fit as usual, and repeat testing
if required.
14-24 Theoretically, there will be nothing in the 5⁄8"[16mm]
sockets, literally a zero thickness wall, where the bit has passed by
twice. However, routing tolerances can leave a very thin “wall”
uncleared by routing. This can be quickly removed with a chisel
or sandpaper.
■
Page 69
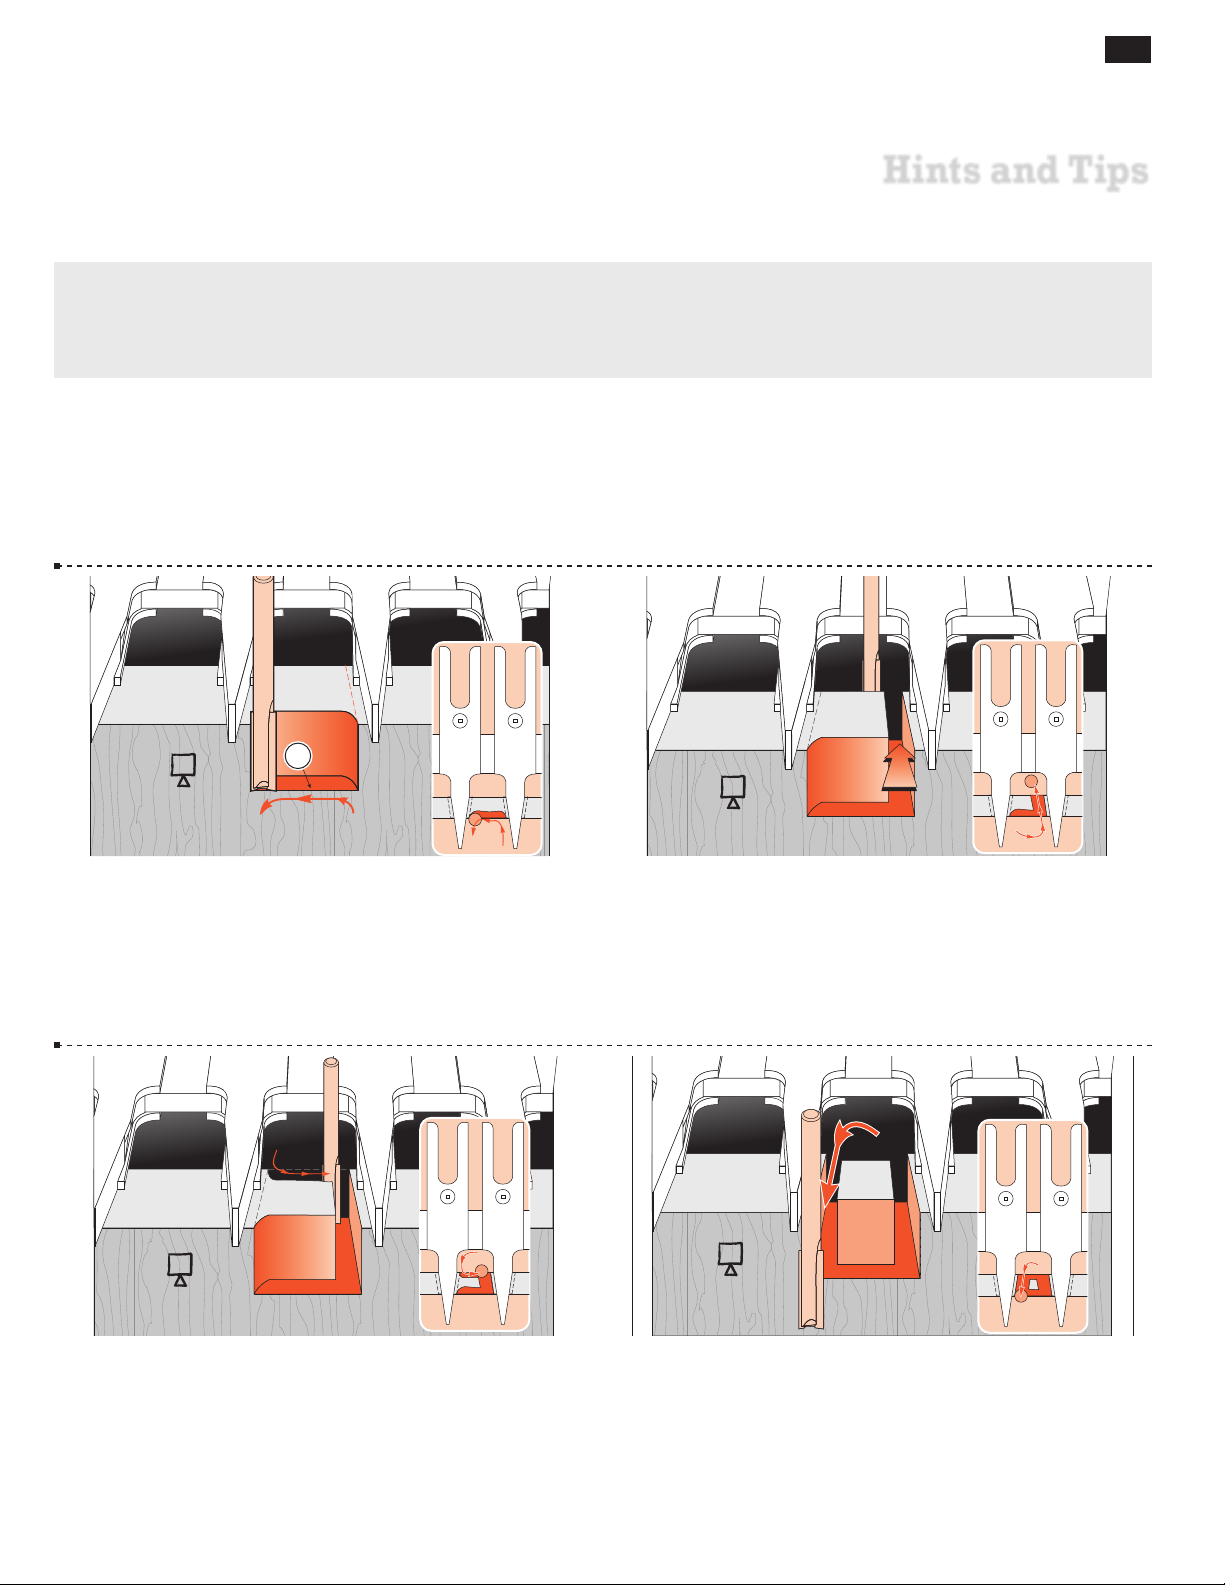
SUPERJIG - CHAPTER 15
Hints and Tips
Here are some special techniques and ideas to help you get the most out of your Leigh Superjig.
63
1
15-1 Through Dovetail Pins With the straight bit, carefully
climb‑rout from right to left. Make sure you control the router
firmly when climb routing.
Climb routing produces a nice clean shoulder at ➀.
Note: For clarity, the guidebush is not shown in this sequence.
15-2
clear of the workpiece. Move the bit to the left side
and climb cut left to right.
Rout through on the right side until the bit is
15-3 Climb rout from left to right from the rear of the cut. Take
care to control router.
15-4
left side.
Rout back through towards you on the
Page 70
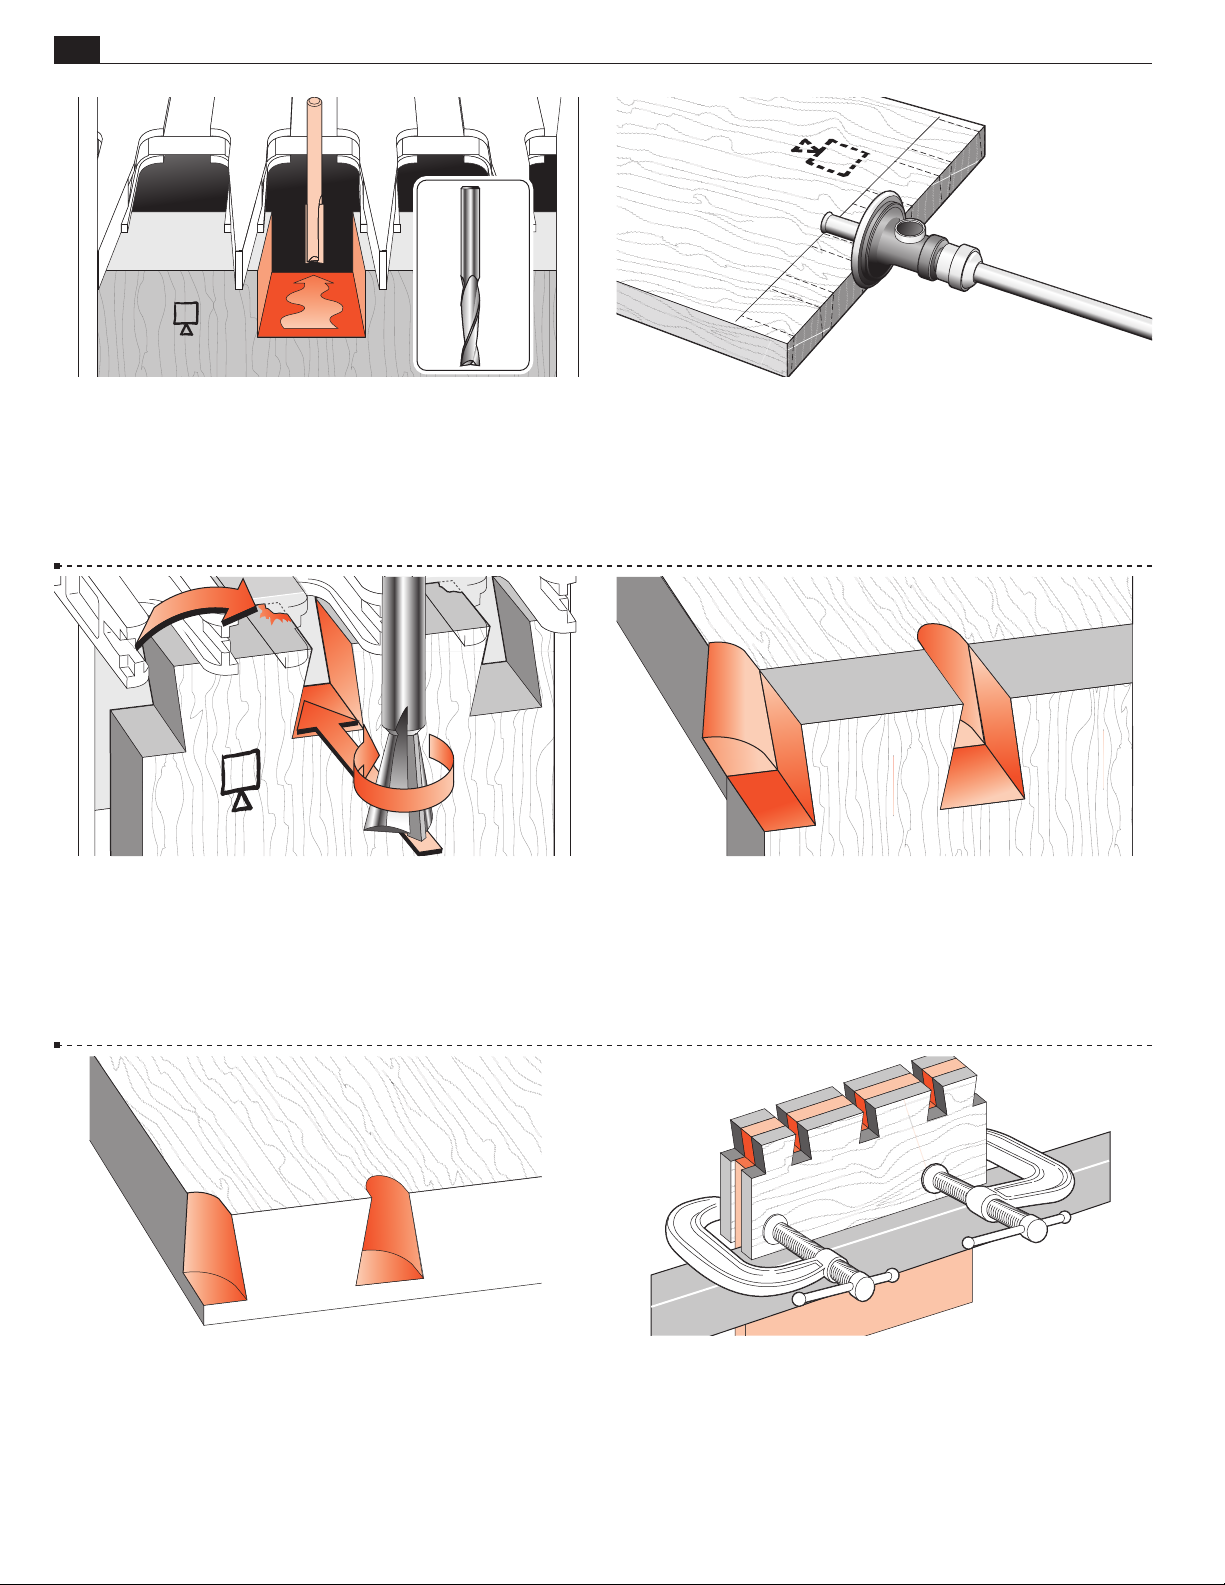
64
Chapter 15 Sup er Jig -12-18-24 User Guide
HINTS AND TIPS
15-5 Rout away the rest of the waste. Note: Spiral up‑cut straight
bits (inset) generally rout more smoothly than the two‑flute
carbide‑tipped bits. If you want to try them, you should be aware
that while the high-speed steel bits take a better edge, they are
much less durable than the more costly solid carbide type (Leigh
bits 170 HSS or 170C solid carbide).
15-7 Dovetail Tails Tearout With the dovetail bit, most
tearout occurs at the top left exit of the cut.
15-6 Preventing TD Pins Tearout To help prevent tearout
at the back bottom part of a straight cut, scribe a line with your
marking gauge across the back of the pin board at exactly the
depth of cut.
15-8 To help prevent this, back up the cut with the end-grain of
a horizontal board pushed against the back of the workpiece and
held in the rear clamp. This board replaces the spacer board.
15-9 This same scrap piece can remain in place for successive
cuts.
15 -10 For vulnerable or that last piece of exotic wood, clamp
horizontal scrap pieces to the front and back of the work piece.
Make sure clamps are below the bit depth.
PLYWOOD is not suitable for routing; the laminates are very
prone to tearout. Either of these two procedures (15-10 or 15-11)
are essential for plywood but provide no guarantee of success.
Page 71
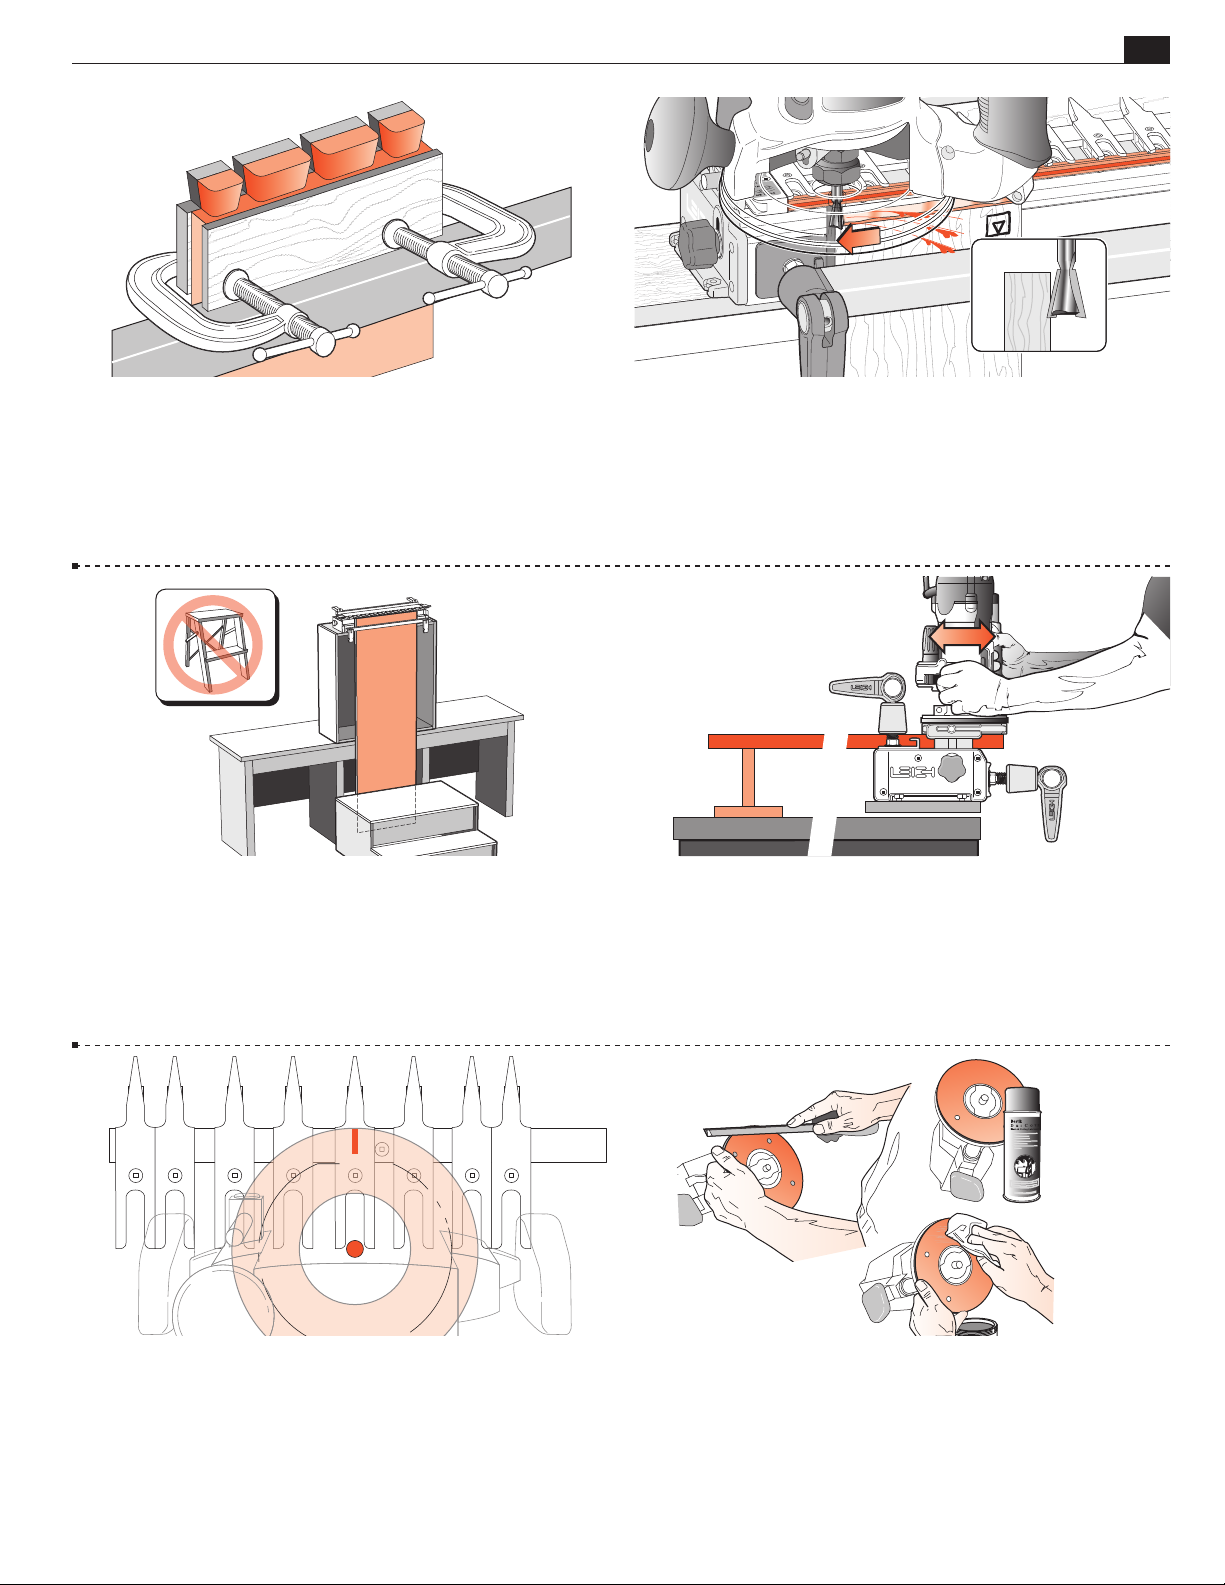
HINTS AND TIPS
Chapter 15Supe rJ ig-12-18-24 User Guide
65
15 -11 A single scrap piece can be C-clamped on the back of halfblind tails, but make sure you protect the workpiece from the clamp
pads. Note: There’s no 100% solution to tearout. It’s not the jig’s
fault, just something that happens when machining, sawing and
even chiseling wood. Important pieces fall off from where you
least want them to.
15-13 General Hints For routing long vertical boards it may
be necessary to build a jig stand to mount securely on your bench.
Make the stand and bench height combination sufficient to accept
the board length you have in mind. The jig stand should be bolted
securely to the bench. Build a stable platform to stand on as in
the illustration. Do not use a set of steps; they’re too unstable.
15 -12 On face cuts, whether using a straight bit or a dovetail bit,
climb routing or back routing will leave a clean edge; but great
caution must be exercised in controlling the router’s movement
from right to left, as the bit rotation pulls the router in that
direction anyway.
15 -14 When placing long horizontal boards in the rear clamp,
make sure the rear end of the board is supported to prevent unnecessary racking of the jig.
15-15 Using The Router Mark the router base top edge at
the 12 o’clock position with a felt marker pen. Without wood or
bits, try some dry runs in each jig mode. This will soon get you
used to positioning the guidebush against the correct guide surface
without looking under the router.
Do not rout at face level.
15 -16 Some router bases have sharp edges on the outside and
inside corners. A slight chamfer of the edges with a fine file or
sandpaper block will ease router movement on the jig.
An occasional light spray of TopCote® or application of soft wax
to the router base makes for smooth, easy router movement on
the jig.
■
Page 72
66
Chapter 15 Sup er Jig -12-18-24 User Guide
HINTS AND TIPS
Page 73
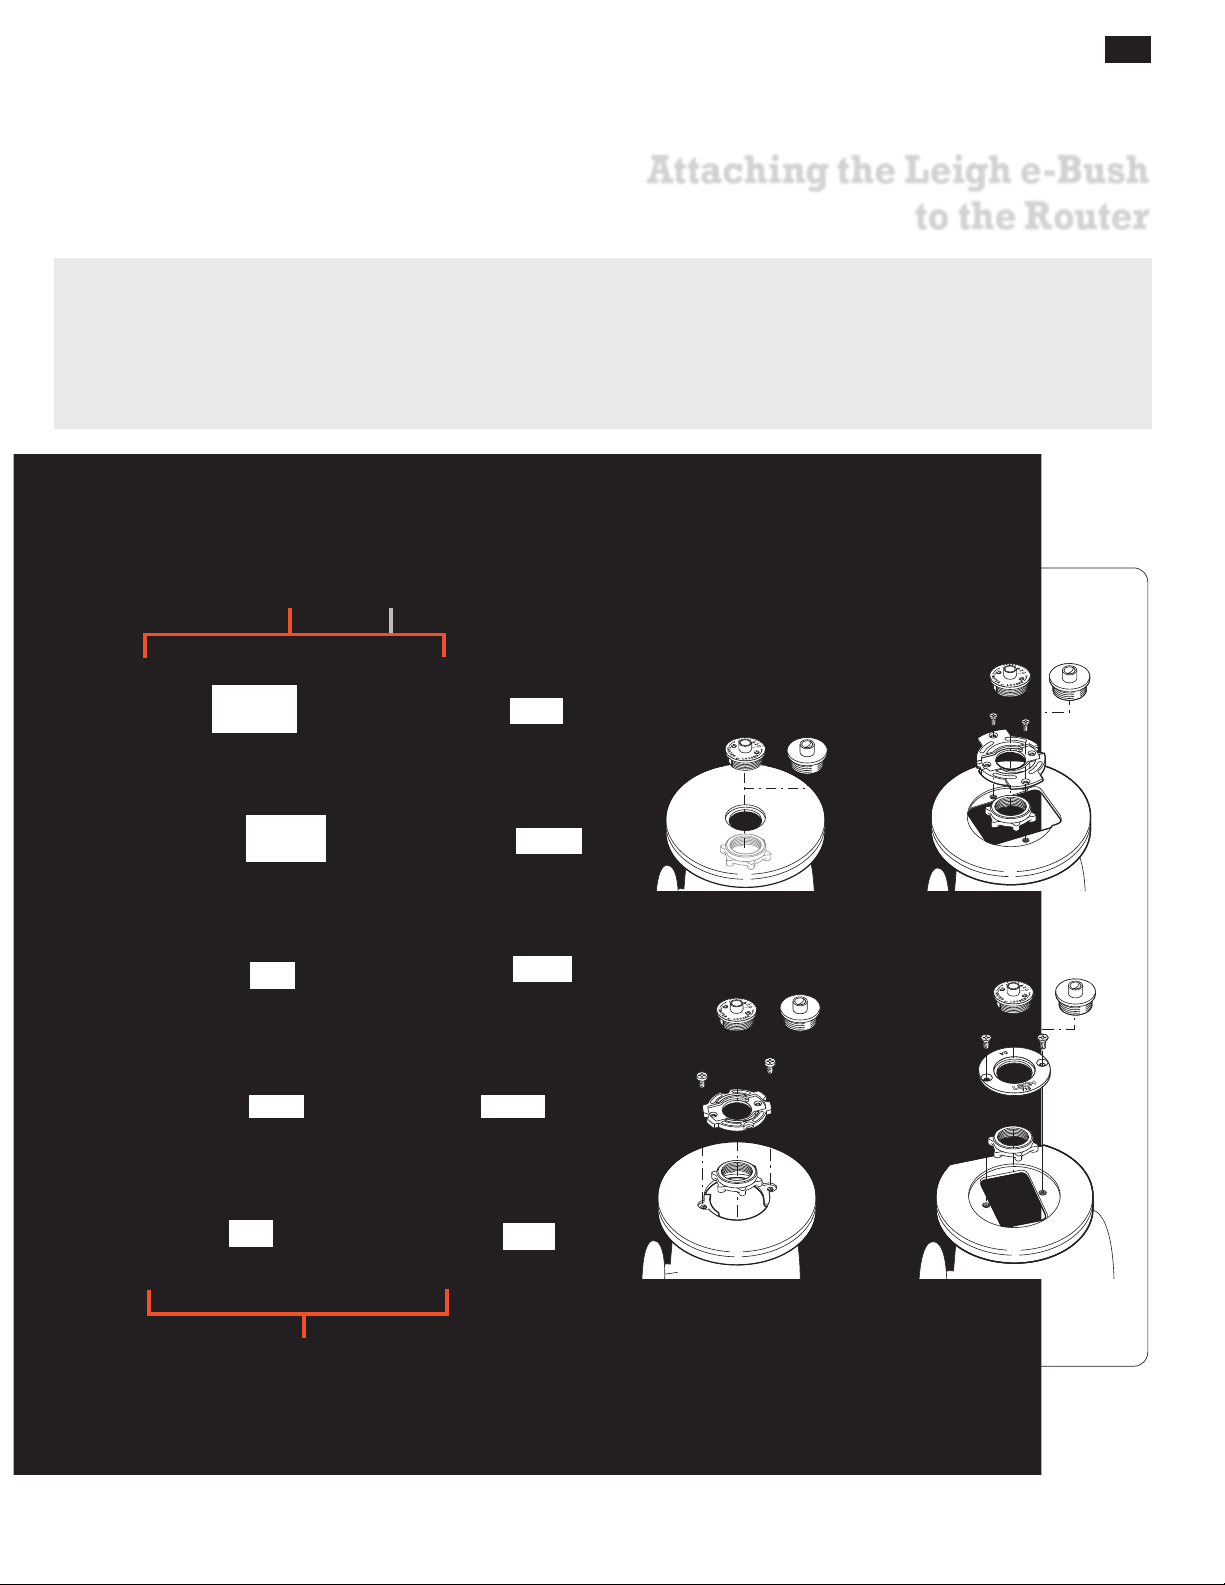
SUPERJIG - Appendix I
Attaching the Leigh e‑Bush
to the Router
e-Bush and Guidebush Adaptors
The Leigh e-Bush fits directly to some popular routers such as Porter Cable, Black & Decker, and Dewalt. Many other makes,
e.g. Bosch, Fein, Festool, Milwaukee etc., offer or come with base adaptors that accept the e-Bush. Leigh offers eight adaptors,
plus the Bosch RA1100 and RA1126, allowing the use of over one hundred other router models, new and old. The 711C
7
⁄16" OD) may be used in place of the e7 for dovetails, however it does not allow fit adjustment for box joints. See the next
(~
page for a list of routers.
e-Bush Adaptors
Optional 711C
e7-Bush
guide bushing is
for dovetails only,
not box joints
e-Bush Mounting Variations
67
Bosch
RA1100
(must be used with
Bosch RA1126 holder)
Bosch
RA1126
(required for
Bosch RA1100)
702
702R
703
706R
710
721
704R
705R
The e7 and 711C fit
directly to many routers
The e7 and 711C with
Adaptor 702 and 702R
Nut for e7
and 711C
The e7 and 711C with
Adaptor 703
The e7 and 711C
with Adaptor 710
Page 74
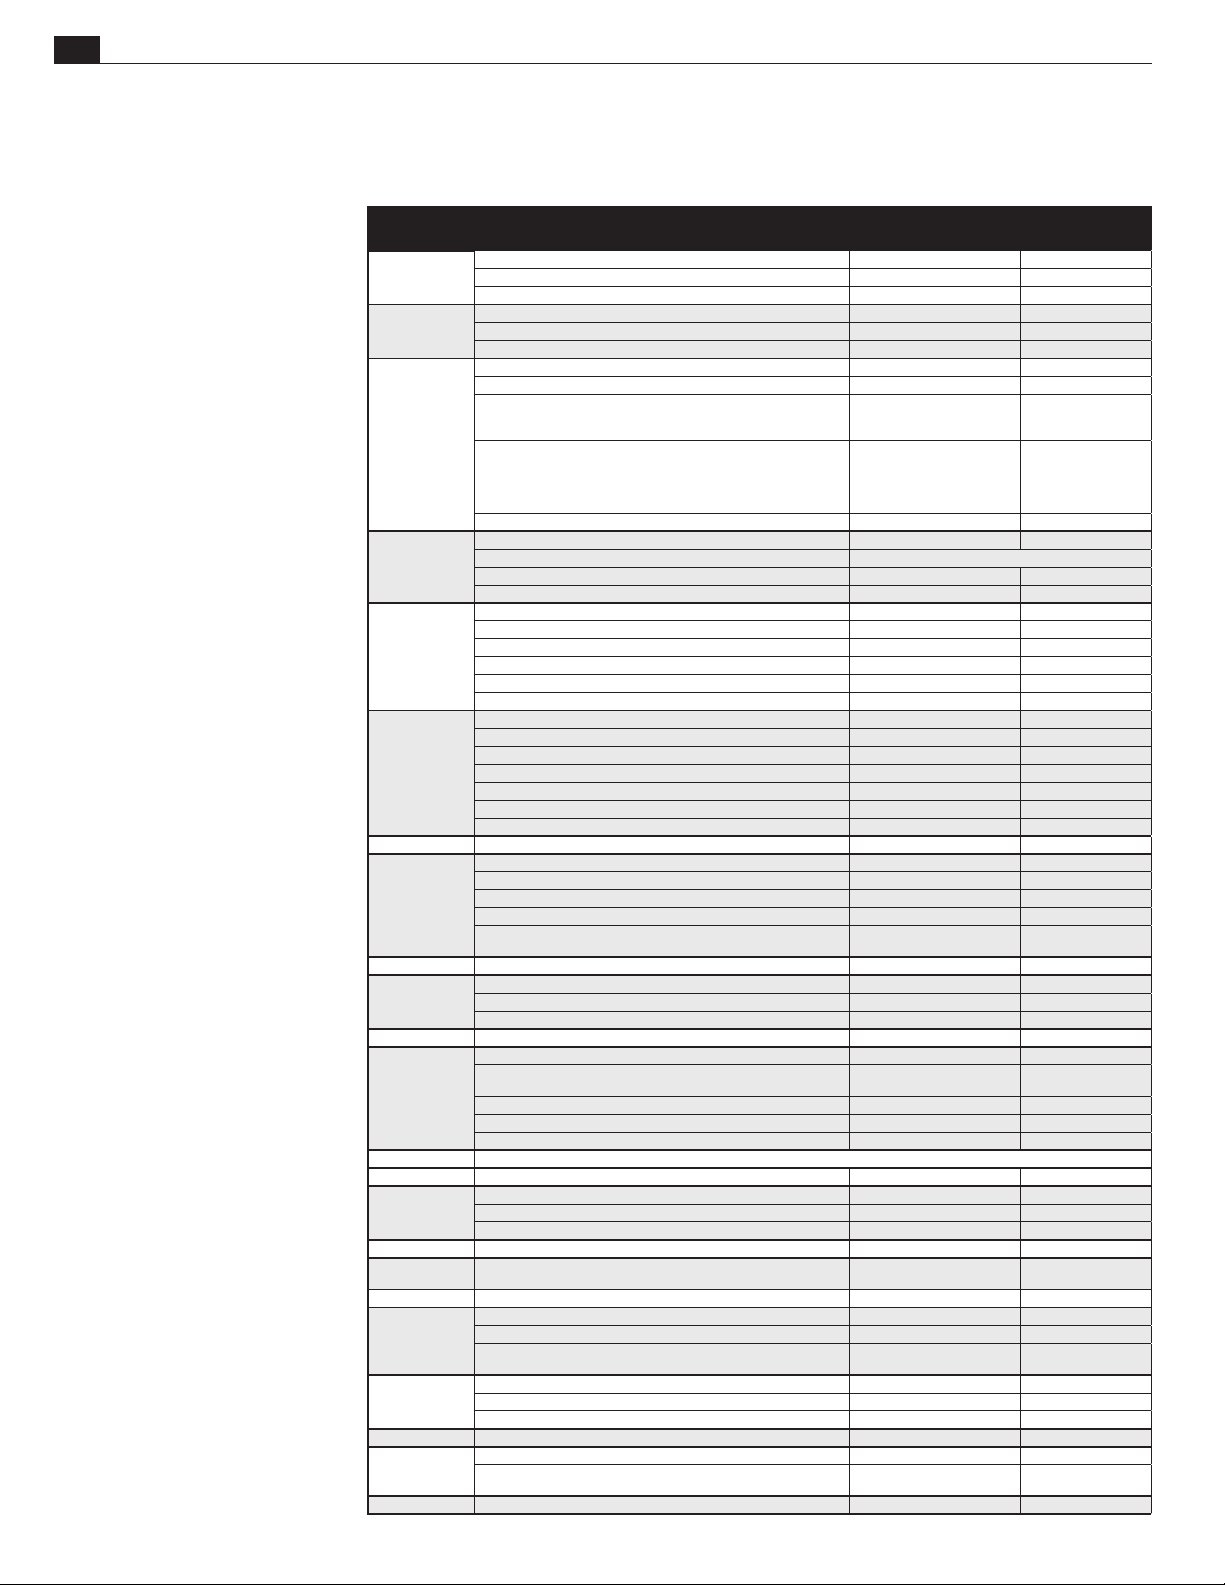
68
Appendix i Sup er Jig -12-18-24 User Guide
ATTACHING THE LEIGH e‑Bush TO A ROUTER
Template Guide Bushing and Adaptor Selection
Your router may need an adaptor to mount the guide bushing. Find out with this chart.
See www.leighjigs.com for the complete list of routers.
DIRECTIONS
A. Locate name of router maker in Column 1.
B. Locate router model in Column 2. If your
router is not listed visit leighjigs.com for a
complete, up-to-date list of routers.
C. Locate adaptor required for your router in
Column 3.
• Order Leigh adaptors (part no’s in red) in
Column 3 from Leigh.
• Order Bosch adaptors RA1100 and
RA1126 in Column 3 from Leigh or your
Bosch dealer.
• Order all other adaptors in Column 3 from
the router manufacturer’s dealer.
Note: Adaptor mounting screws are included
with router.
■
MAFELL – Rework adaptor slightly.
D. Guide bushings in Column 4 fit all adaptors
listed and may be ordered if required.
◆ A ~
7/16" e7 guide bushing is supplied
with all Leigh Super jigs. Order only if
you require a replacement.
All 8mm shank bits work with the e7-Bush
supplied with your Leigh jig, or with any
7/16
" OD guide bushing that has a min.
barrel length of 1/4". No other guide bushing
sizes can be used.
Note: The 711C (~
7/16
" OD guide bushing)
has replaced the 711TP.
ROUTER
1
MAKER
AEG
BLACK & DECKER
1600, 90085, 90088, 90098, 90140, 90150, 90300, 90303, 90305, 91264 Aftermarket base plate required e7 or 711C/711TP
North American ROUTERS PRODUCED AFTER mid-2010: 1613EVS, 1613AEVS,
1617, 1617EVS, 1618, 1618EVS, 1619EVS, MR23EVS, MRC23EVS, MRF23EVS,
BOSCH
CRAFTSMAN
(SEARS)
DEWALT
ELU
FEIN RT1800 Supplied w/router e7 or 711C/711TP
FESTOOL
FREUD FT700(2), FT2000, FT2200, FT3000 721 e7 or 711C/711TP
HITACHI
MAFELL LO65E 702
MAKITA
MASTERCRAFT
METABO OF1612, OFE1812 (for all others, please contact Leigh for assistance) 704R e7 or 711C/711TP
MILWAUKEE
PERLES OF808 Series, OFE6990 710 e7 or 711C/711TP
PORTER CABLE
(ROCKWELL)
RIDGID R2930 (for all others, please contact Leigh for assistance) 704R e7 or 711C/711TP
RYOBI
SKIL
TREND T3, T4, T5, T9, T10, T11–UniBase required 710 e7 or 711C/711TP
TRITON
WEGOMA OF850 Series 710 e7 or 711C/711TP
North American ROUTERS PRODUCED BEFORE mid-2010 and others available
worldwide that include the RA1126 adaptor: 1613, 1613EVS, 1613AEVS,
1614, 1614EVS, 1617EVS, 1618EVS, 1619EVS, B1450, GOF900, GOF900CE,
GOF900ACE, GOF1200, GOF1300CE, GOF1300ACE, GOF1600CE, GOF2000CE,
GMF1400, GMF1600CE, POF800ACE, POF1100AE, POF1200AE, POF1400ACE
M363, MRP090, RP1800, RP1801, RP2301, RP2301FC, 3612C Europe Qk Fit Base 721 e7 or 711C/711TP
3600, 3606, 3608, 3612, 3612B, 3612BR, 3612C N. America, 3620, 3621,
Please contact Leigh for assistance
All Professional, HD1250, RP400K,7614 Not Required e7 or 711C/711TP
SR100, 7AEE, KW780 series, KW 800, KW850 710 e7 or 711C/711TP
1601, 1602, 1603, 1604, 1606, B1350 RA1110 e7 or 711C/711TP
1611, 1611EVS, 1615, 1615EVS, B1550, GOF1600, GOF1700ACE 702 e7 or 711C/711TP
MD11 Plunge & Fi xed Base. MD9.5 F ixed Bas e Not Required e7 or 711C/711TP
DW614, DW615, DW621, DW624, DW625, DW626 N. America Only, Supplied w/router e7 or 711C/711TP
DW621K & DW626 outside N. America 706R e7 or 711C/711TP
DW625 Type 1,2,3,5 outside N. America 702 e7 or 711C/711TP
DW624 & DW625 Type 4 outside N.America, DW625EK 702R e7 or 711C/711TP
OF1E , OF2E, OF650, OF900E ,OF1000, OF1010E 704R e7 or 711C/711TP
OF1400 and OF2200 North America Only Supplied w/router e7 or 711C/711TP
RF1100, RF1101, RD1100, RD1101, RP1101 Not Required e7 or 711C/711TP
R30, R50, R150, R151, RE155, R500, R501, R502 703 e7 or 711C/711TP
R160, R161, R162, R163K, R165, R170,
R175, RE175, R180, R180PL, R181, R185, ERT1150
ROUTER
2
MODEL
OFE 710 in plunge base Not Required
OFSE 2000 703
RT1350E 706R
6200 720673-00 e7 or 711C/711TP
MRP23EVS
All non-plunge models Aftermarket base plate required e7 or 711C/711TP
135275070 Plunge See Skil 1823 or 1835
Other plunge models 702 e7 or 711C/711TP
DW610, DW616, DW618 Not Required e7 or 711C/711TP
DW613, DW615(UK) 710 e7 or 711C/711TP
OF15, OF15E, OF97, OF97E 706R e7 or 711C/711TP
MOF68, MOF69, MOF96, MOF96E 710 e7 or 711C/711TP
MOF131, MOF177 Type 1,2, & 3 702 e7 or 711C/711TP
MOF177 Type 4, MOF177EK 702R e7 or 711C/711TP
2720, 2721, 3328 Not Required e7 or 711C/711TP
3303, 3304 EO9600 or 761 270-00 e7 or 711C/711TP
3337, 3338, 3339 702 e7 or 711C/711TP
OF2000, OF2000E 705R
OF1400 Outside North America 493566 e7 or 711C/711TP
OF2200 Outside North America
TR8, TR12, FM8, M8, M12 Series 325211 OR 703 e7 or 711C/711TP
M12VC, KM12SC, KM12VC Not Required e7 or 711C/711TP
M12SA2, M12V2 325224 e7 or 711C/711TP
RP0900, RP900K
3601B 321 493-1 e7 or 711C/711TP
RP0910, RP1110C 706R e7 or 711C/711TP
5615, 5616, 5619 49-54-1040 e7 or 711C/711TP
5625 49-54-1026 e7 or 711C/711TP
5670 Not Required e7 or 711C/711TP
All Not Required or Supplied w/router e7 or 711C/711TP
R600, R601, RE600, RE601 702 e7 or 711C/711TP
1823 or 1835 91803 e7 or 711C/711TP
SK1810, 1815, 1820, 1825 RAS140 e7 or 711C/711TP
All others Aftermarket base plate required 11592
TRC001 TGA006 or 704R e7 or 711C/711TP
JOF001, MOF001, TRA001
ROUTER
3
ADAPTOR
RA1126 quick change adaptor and
RA1100 bushing adaptor req’d
RA1100 e7 or 711C/711TP
494627 O-Ring may be required
to keep bushing centered
■ e7 or 711C/711TP
703 e7 or 711C/711TP
706R e7 or 711C/711TP
Accessory Kit (includes adaptor)
TGA001 or TGA150
7/16" OD
4
BUSHING
e7 or 711C/711TP
e7 or 711C/711TP
e7 or 711C/711TP
e7 or 711C/711TP
e7 or 711C/711TP
e7 or 711C/711TP
e7 or 711C/711TP
◆
Page 75
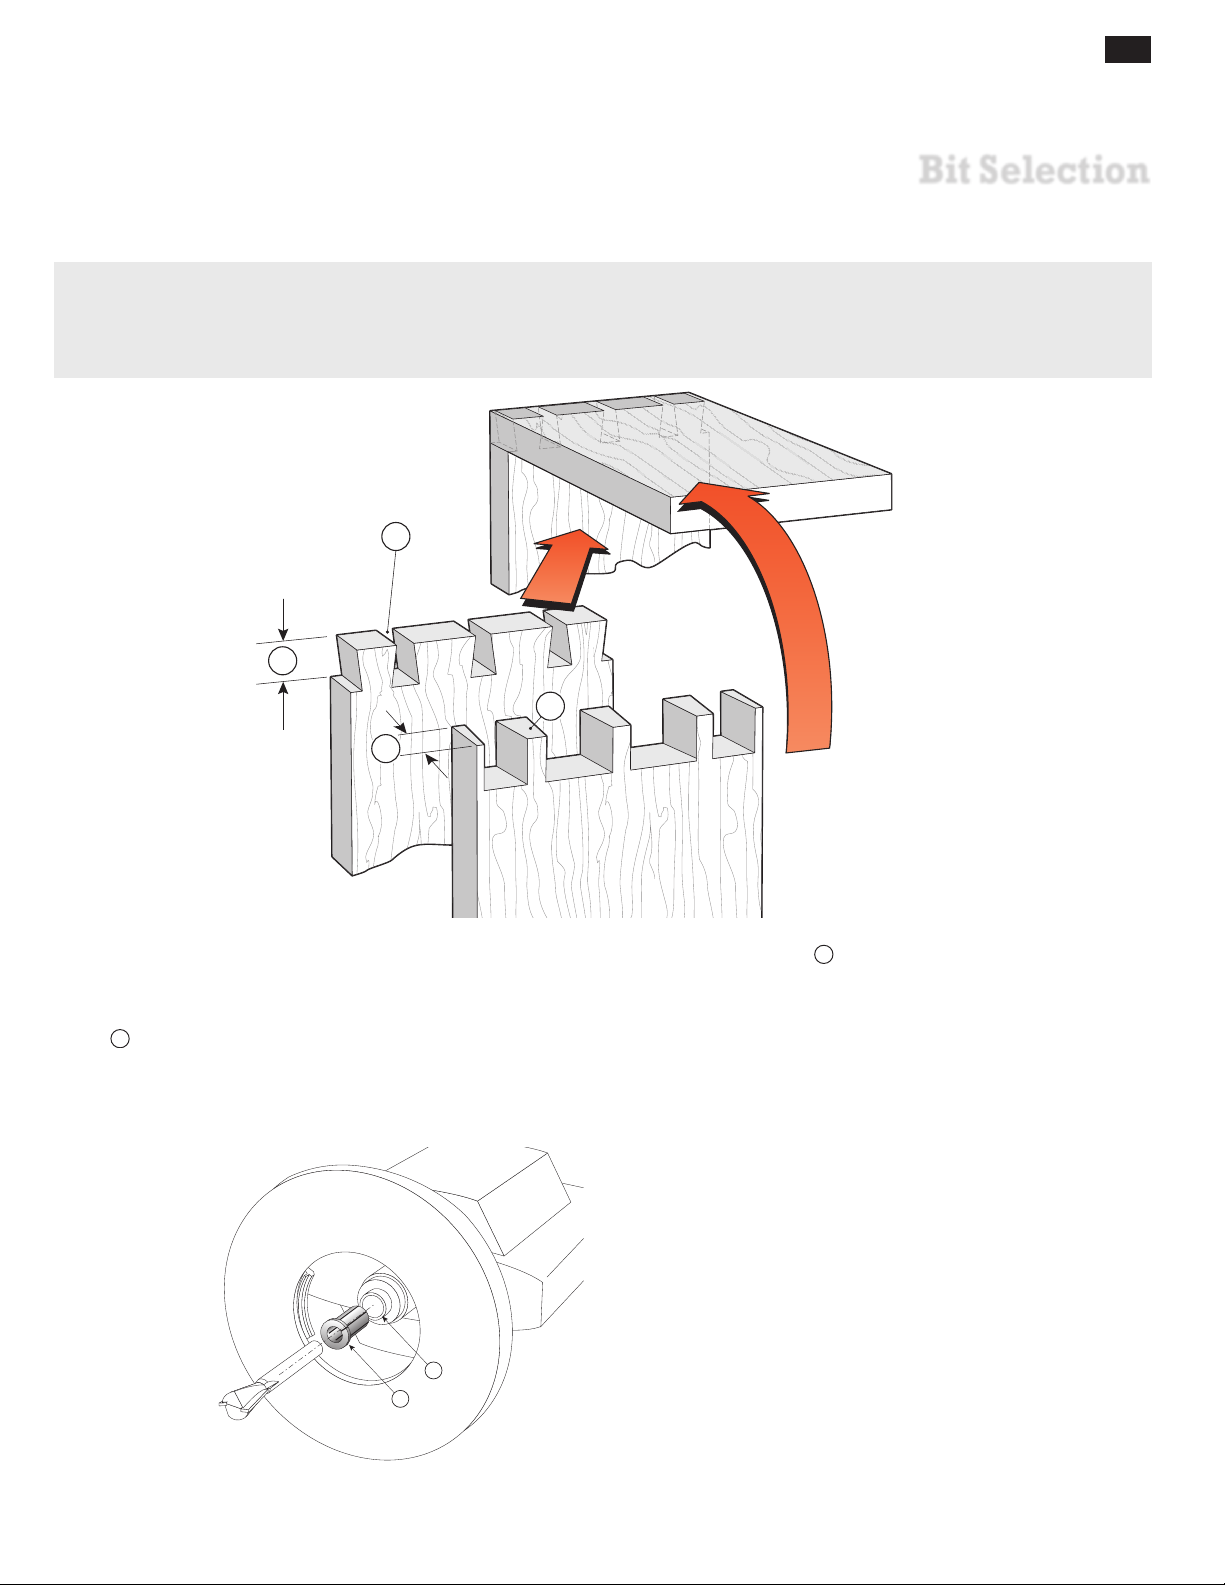
Optional router bits for variably spaced through and half‑blind dovetails.
2
1
B
3
Through Dovetails
69
SUPERJIG - Appendix II
Bit Selection
Bit Selection for Through Dovetails
8° Dovetail Bit for Tails
The pins ➀ must fit into the sockets ➁. So the dovetail bit’s depth
of cut B must be equal to or a little greater than the pinboard
thickness ➂.
Measure the pinboard thickness ➂ and select the dovetail bit with
5
4
the correct depth of cut B from the following pages (bits must be
8° for through dovetails).
Straight Bit for Pins
The matching straight bit is listed just below the dovetail bits. The
5
⁄16" diameter No. 140-8, 8mm shank is the only straight bit you
need with the Superjig.
Guidebush
All joints on the Superjig are routed with the e7-Bush, or all but
7
box joints with any ~
⁄16" OD guidebush (min. barrel depth 1⁄4").
See page 68.
Shank Selection
Note: You will require a router with an 8mm or 1⁄2"[12,7mm] collet
1
to use our 8mm shank bits. For a
1
will require our
⁄2"[12,7mm] to 8mm collet reducer No. 172‑8.
⁄2"[12,7mm] collet router you
Note: This is a collet reducer ➃, not a collet ➄. It does not replace
1
the collet, it slides directly into your
⁄2" collet. Do not remove
the collet nut when installing the collet reducer.
Page 76
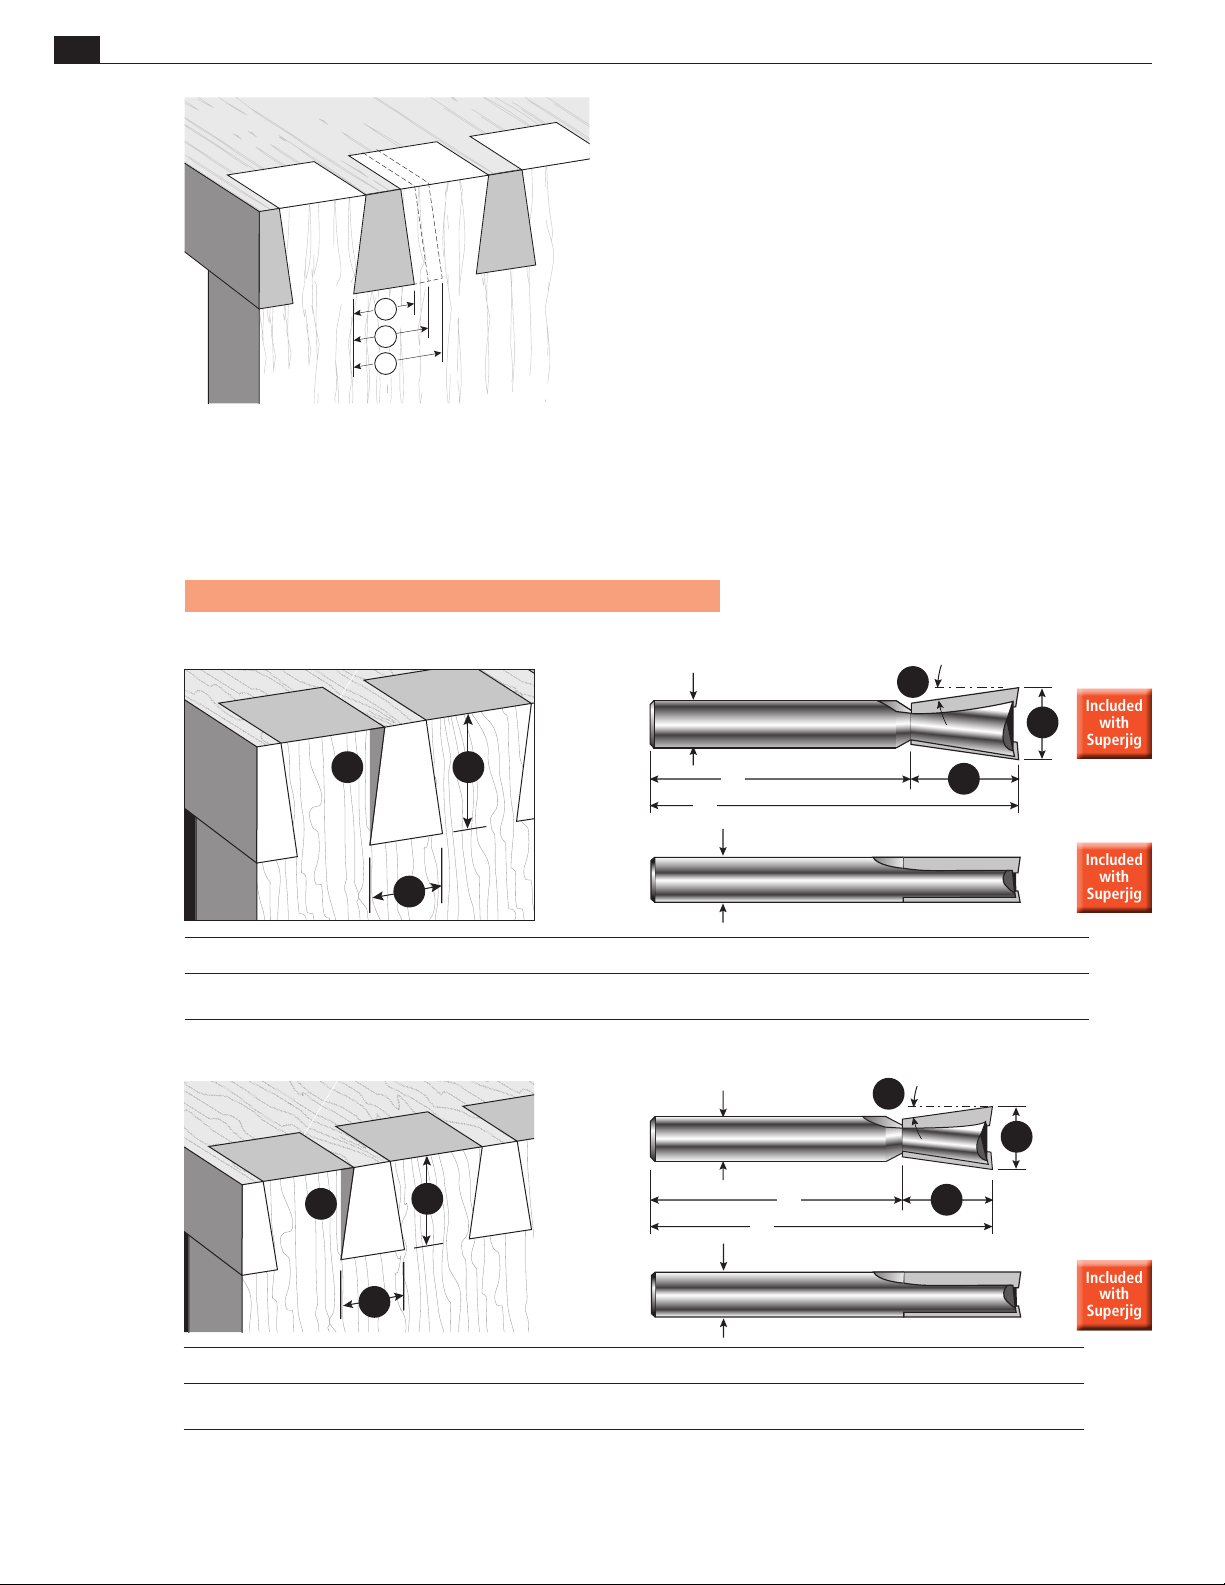
70
2
3
1
E
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Appendix ii Sup er Jig -12-18-24 User Guide
Note: Bit and joint drawings are about actual size.
BIT SELECTION
You will note that some of the dovetail bits’ depths of cut overlap.
For example:
No. 80-8 bit (B): 1⁄2"– 13⁄16"[12 - 20mm]
No. 70-8 bit (B): 1⁄4"–1⁄2"[6 - 12mm]
1
This means that
⁄2" boards can be joined using either the
No. 80-8 and 140-8 combination, the No. 75-8 and 140-8 combination, or the No. 70-8 and 140-8 combination.
The three bit combinations will produce slightly different-looking
joints because each dovetail bit produces a different size pin:
3
No. 70-8
No. 75-8 7⁄16"
⁄8"
➀
➁
No. 80-8 1⁄2" ➂.
Do not attempt to rout dovetails at less than the minimum
depth of cut specified.
Leigh Through Dovetail Bits
C
80-8
F
A B C D E F Guidebush
Bits Overall Diameter Cutting Depth Range Shank Diameters Shank Length Overall Length Angle Diameter
No. 80-8* 1/2" [12,7] 1/2" to 13/16" [13,0-20,6]** 8mm 1-3/4" [45,0] 2-9/16" [65,0] 8° e7 or 711C ~7/16" [11,1]
No. 140-8* 5/16" [7,9] up to 1" [26,0] 8mm 1-3/4" [45,0] 2-3/4" [70,0] – e7 or 711C ~7/16" [11,1]
F
B
A
140-8
75-8
B
D
E
C
C
D
F
A
B
F
A
B
C
A
A B C D E F Guidebush
Bits Overall Diameter Cutting Depth Range Shank Diameters Shank Length Overall Length Angle Diameter
No. 75-8 7/16" [11,1] 3/8" to 5/8" [9,5-16,0] 8mm 1-3/4" [45,0] 2-3/8" [60,0] 8° e7 or 711C ~7/16" [11,1]
No. 140-8* 5/16" [7,9] up to 1" [26,0] 8mm 1-3/4" [45,0] 2-3/4" [70,0] – e7 or 711C ~7/16" [11,1]
Numbers in brackets are millimeters * Bits 80-8, 120-8, and 140-8 come standard with Leigh Super Jigs
**Maximum pin board thickness = 13⁄16"
140-8
Page 77
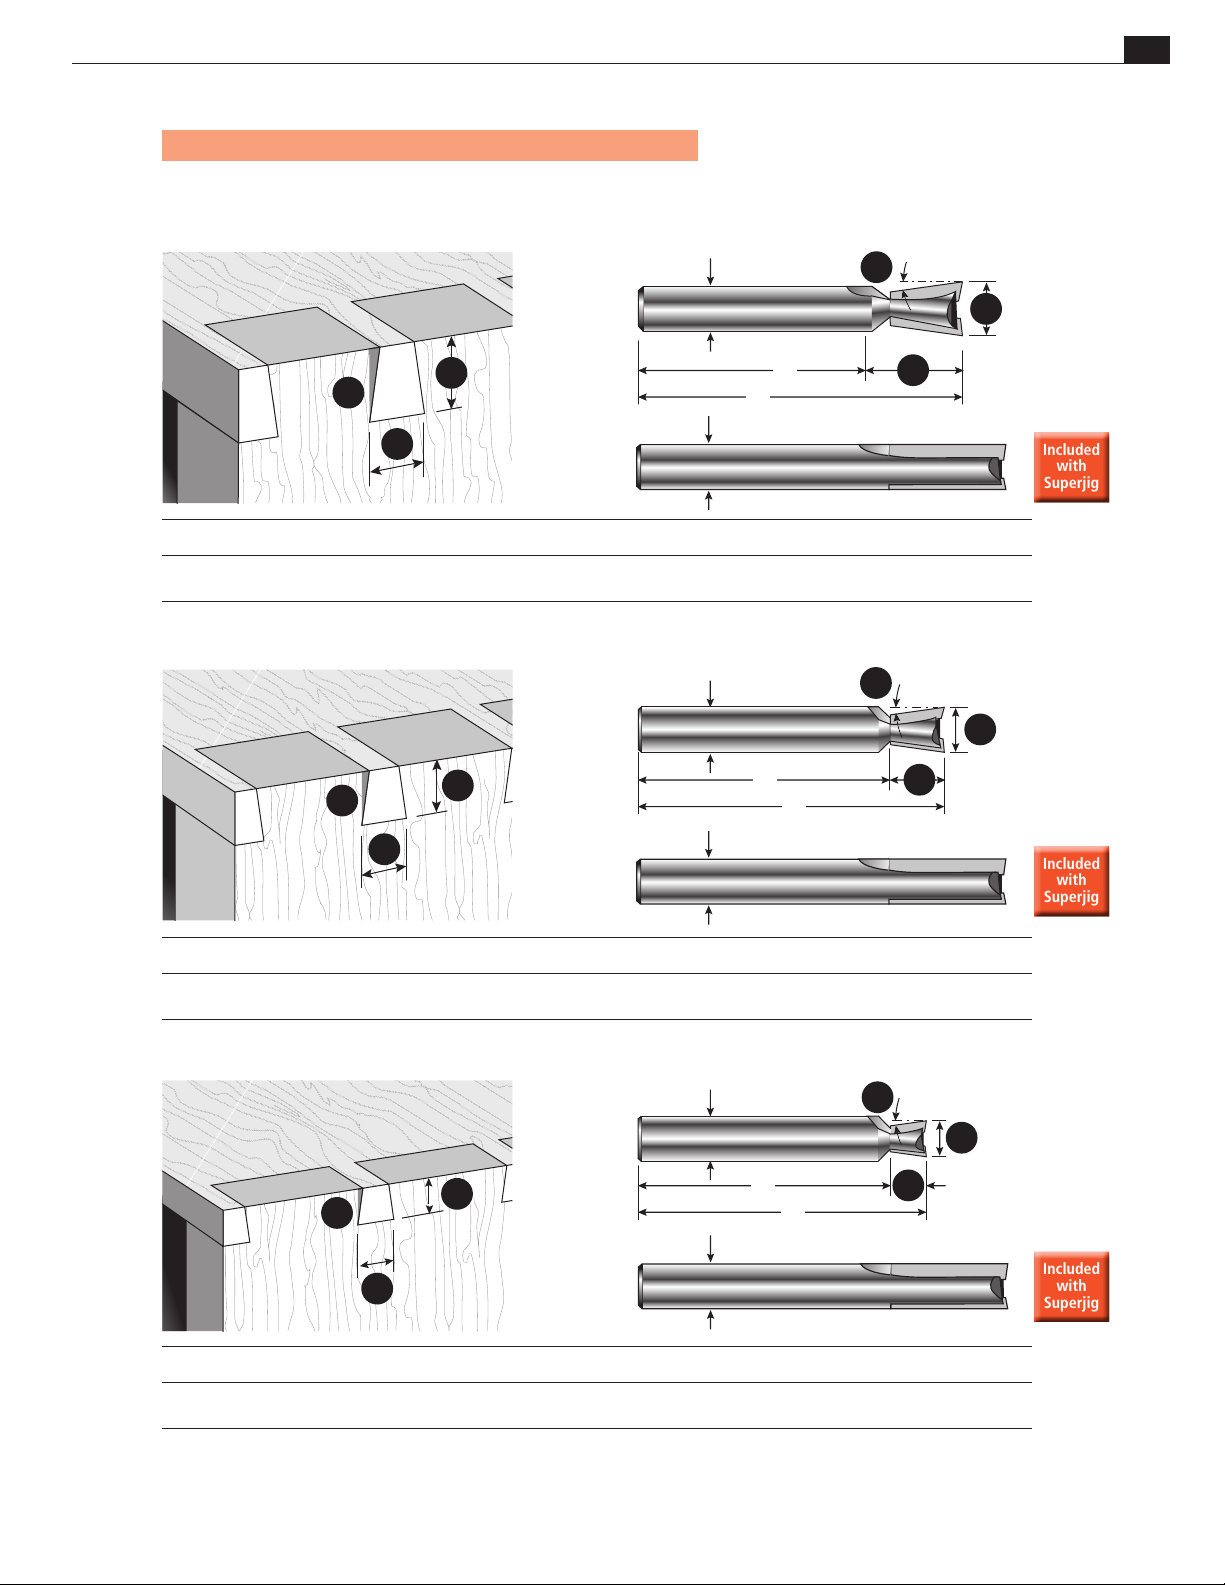
BIT SELECTION
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Included
with
Superjig
Note: Bit and joint drawings are about actual size.
Leigh Through Dovetail Bits
Appendix iiSu per Ji g-12-18-24 User Guide
71
C
70-8
F
B
A
C
D
E
F
A
B
140-8
A B C D E F Guidebush
Bits Overall Diameter Cutting Depth Range Shank Diameters Shank Length Overall Length Angle Diameter
No. 70-8 3/8" [9,5] 1/4" to 1/2" [6,0-13,0] 8mm 1-3/4" [45,0] 2-1/4" [57,0] 8° e7 or 711C ~7/16" [11,1]
No. 140-8* 5/16" [7,9] up to 1" [26,0] 8mm 1-3/4" [45,0] 2-3/4" [70,0] – e7 or 711C ~7/16" [11,1]
C
60-8
F
A
B
C
D
E
F
A
B
140-8
A B C D E F Guidebush
Bits Overall Diameter Cutting Depth Range Shank Diameters Shank Length Overall Length Angle Diameter
No. 60-8 5/16" [7,9] up to 3/8" [9,5] 8mm 1-3/4" [45,0] 2-1/8" [54,0] 8° e7 or 711C ~7/16" [11,1]
No. 140-8* 5/16" [7,9] up to 1" [26,0] 8mm 1-3/4" [45,0] 2-3/4" [70,0] – e7 or 711C ~7/16" [11,1]
C
50-8
F
B
D
E
F
A
B
C
A
A B C D E F Guidebush
Bits Overall Diameter Cutting Depth Range Shank Diameters Shank Length Overall Length Angle Diameter
No. 50-8 1/4" [6,35] up to 1/4" [6,35] 8mm 1-3/4" [45,0] 2" [50,0] 8° e7 or 711C ~7/16" [11,1]
No. 140-8* 5/16" [7,9] up to 1" [26,0] 8mm 1-3/4" [45,0] 2-3/4" [70,0] – e7 or 711C ~7/16" [11,1]
Numbers in brackets are millimeters * Bits 80-8, 120-8, and 140-8 come standard with Leigh Super Jigs
140-8
Page 78
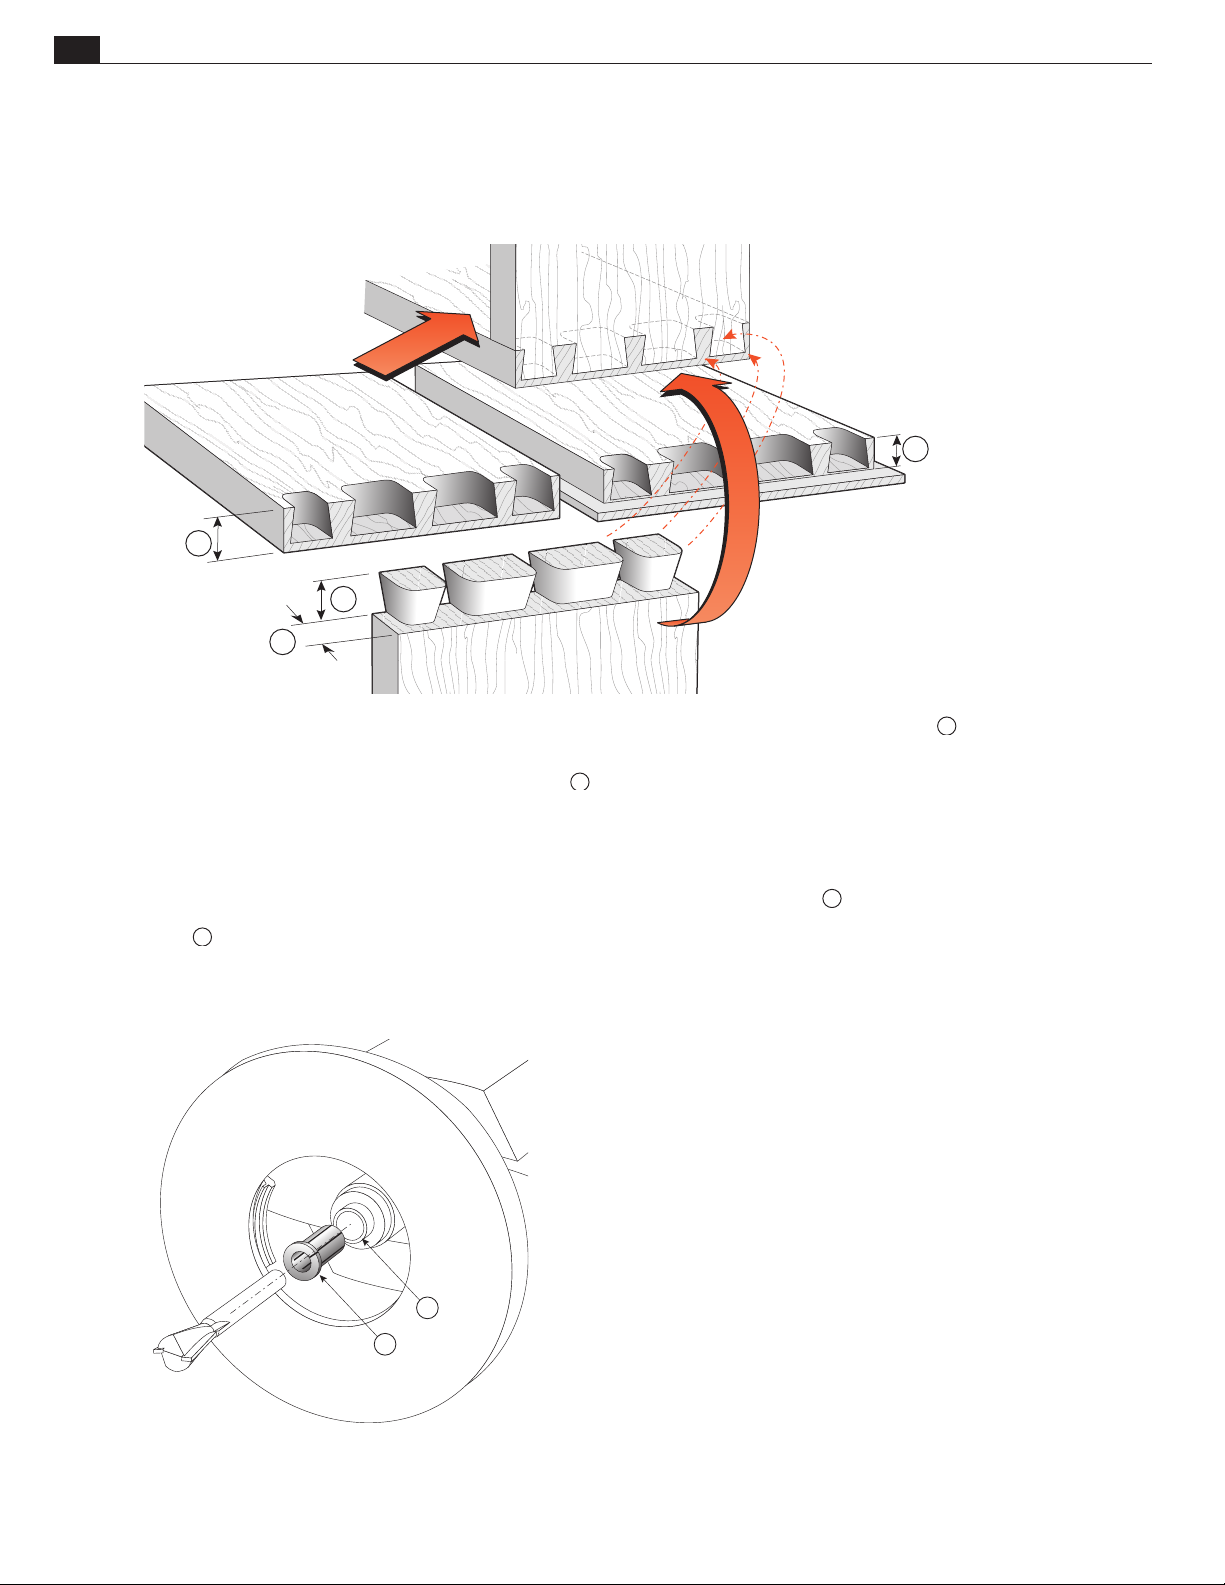
72
B
B
4
5
Appendix ii Sup er Jig -12-18-24 User Guide
Half-Blind Dovetails
1
B
BIT SELECTION
2
3
Bit Selection for Half-Blind Dovetails
Both parts of a half-blind dovetail are cut with the same
dovetail bit. The dovetail bit’s working depth of cut B
must be less than the pinboard thickness ➀ for flush
1
drawers by at least
⁄8"[2mm], and slightly less than the
rabbet depth ➁ for rabbeted drawer fronts. Minimum
1
pin board (drawer front) thickness is
⁄2"[12mm].
Drawer side thickness ➂ does not affect bit selection.
Note:
is the nominal working depth for half‑blind
dovetails, not the maximum depth. B must
not be varied, except for minor adjustments for
joint fit. See page 35.
Measure the drawer front thickness (minimum
1
⁄2"[12mm]) ➀ or rabbet depth (minimum
7
⁄16"[11,1mm]) ➁ and select the bit with the
appropriate depth of cut
from one of the five
bits on the following pages.
Guidebush
All joints on the Superjig are routed with the
e7-Bush, or all but box joints with any 7⁄16" OD
1
guidebush (min. barrel depth
⁄4"). See page 68.
Shank Selection
Note: You will require a router with an 8mm or
1
⁄2"[12,7mm] collet to use our 8mm shank bits.
1
⁄2 "[12,7mm] collet you will require our
For a
1
⁄2"[12,7mm] to 8mm collet reducer No. 172‑8.
Note: This is a collet reducer ➃, not a collet ➄.
It does not replace the collet, it slides directly
1
into your
⁄2" collet. Do not remove the collet
nut when installing the collet reducer.
Page 79
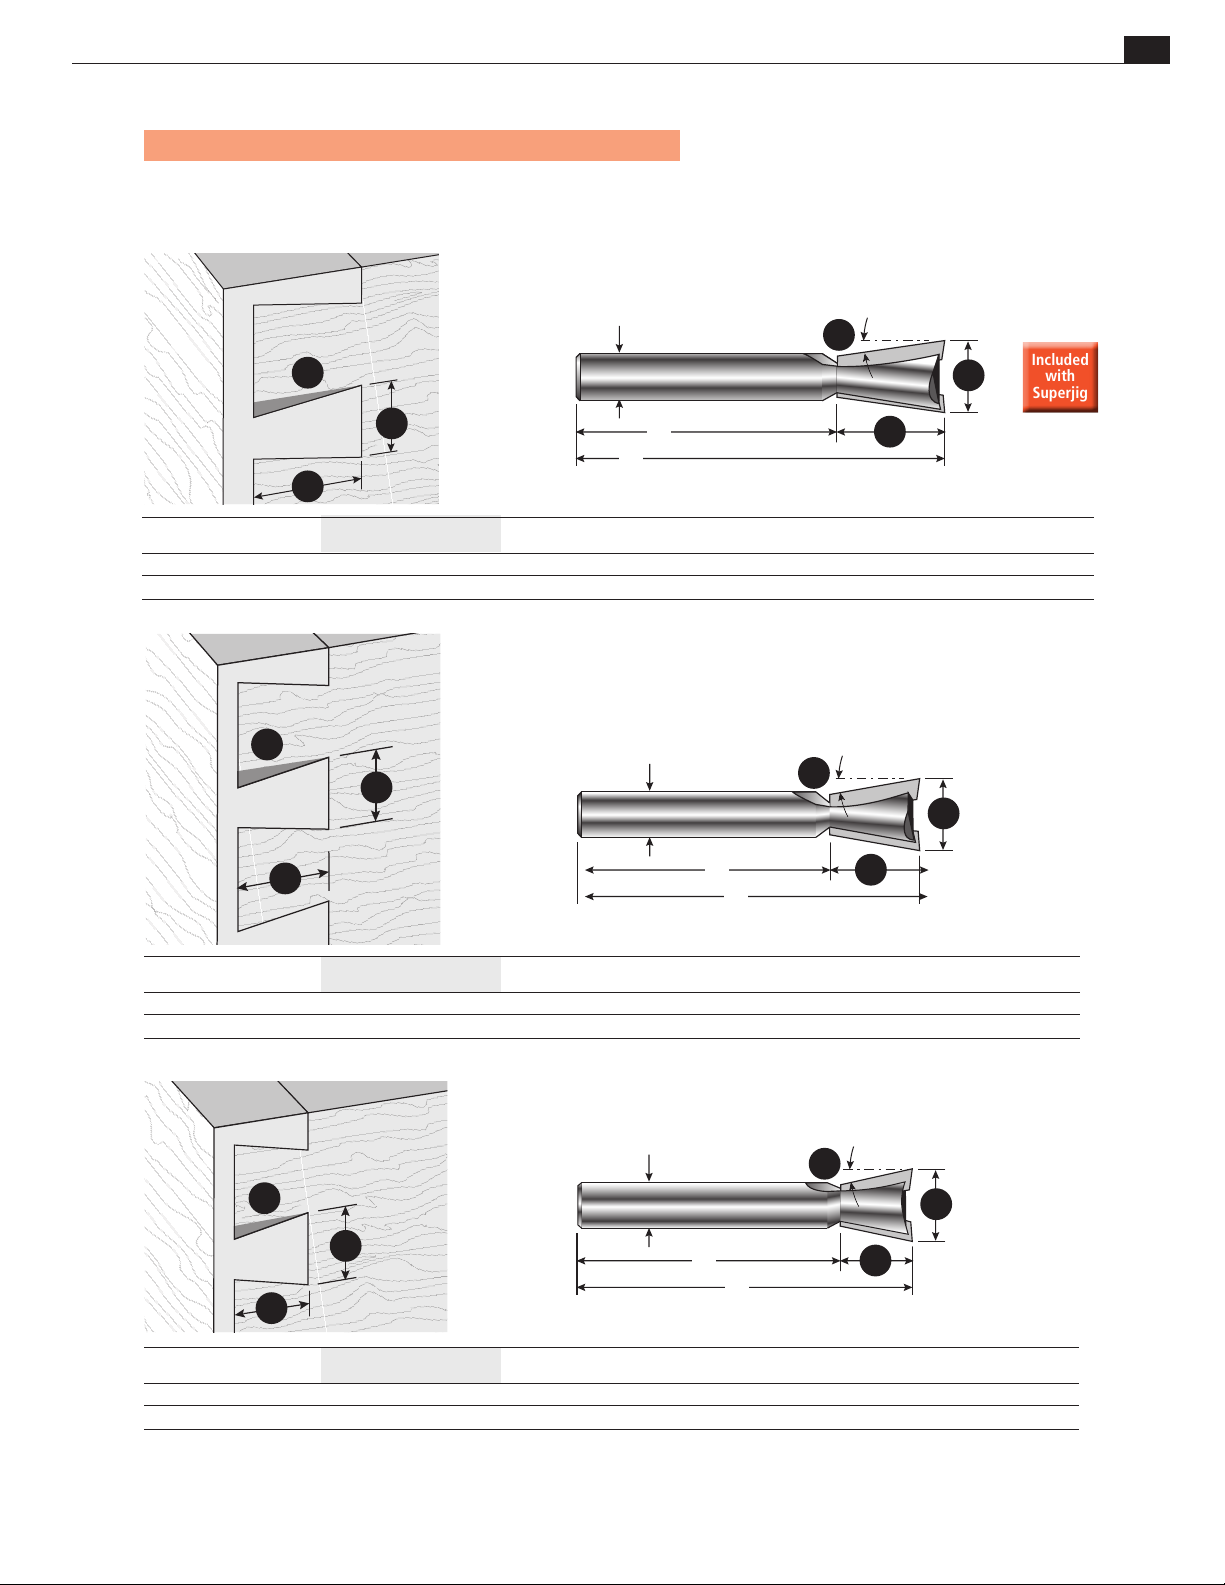
BIT SELECTION
Included
with
Superjig
Included
with
Superjig
Note: Bit and joint drawings are about actual size.
Leigh Half-Blind Dovetail Bits
Appendix iiSu per Ji g-12-18-24 User Guide
73
C
F
A
80-8
D
E
F
A
B
B
A B C D E F Guidebush
Bits Overall Diameter Working Depth Shank Diameters Shank Length Overall Length Angle Diameter
HB Variable HB 1-Pass
No. 80-8* 1/2" [12,7] ~3/4" [19] ~1/2" [12,7] 8mm 1-3/4" [45,0] 2-9/16" [65,0] 8° e7 or 711C ~7/16" [11,1]
F
A
101-8
B
C
D
E
F
A
B
A B C D E F Guidebush
Bits Overall Diameter Working Depth Shank Diameters Shank Length Overall Length Angle Diameter
HB Variable HB 1-Pass
No. 101-8 1/2" [12,7] ~5/8" [16,0] ~7/16"[11,1] 8mm 1-3/4" [45,0] 2-3/8" [60,0] 10° e7 or 711C ~7/16" [11,1]
C
F
A
112-8
D
E
F
A
B
B
A B C D E F Guidebush
Bits Overall Diameter Working Depth Shank Diameters Shank Length Overall Length Angle Diameter
HB Variable HB 1-Pass
No. 112-8 1/2" [12,7] ~1/2" [13,0] ~3/8" [9,5] 8mm 1-3/4" [44,0] 2-21/64" [59] 12° e7 or 711C ~7/16" [11,1]
Numbers in brackets are millimeters * Bits 80-8, 120-8, and 140-8 come standard with Leigh Super Jigs
Page 80
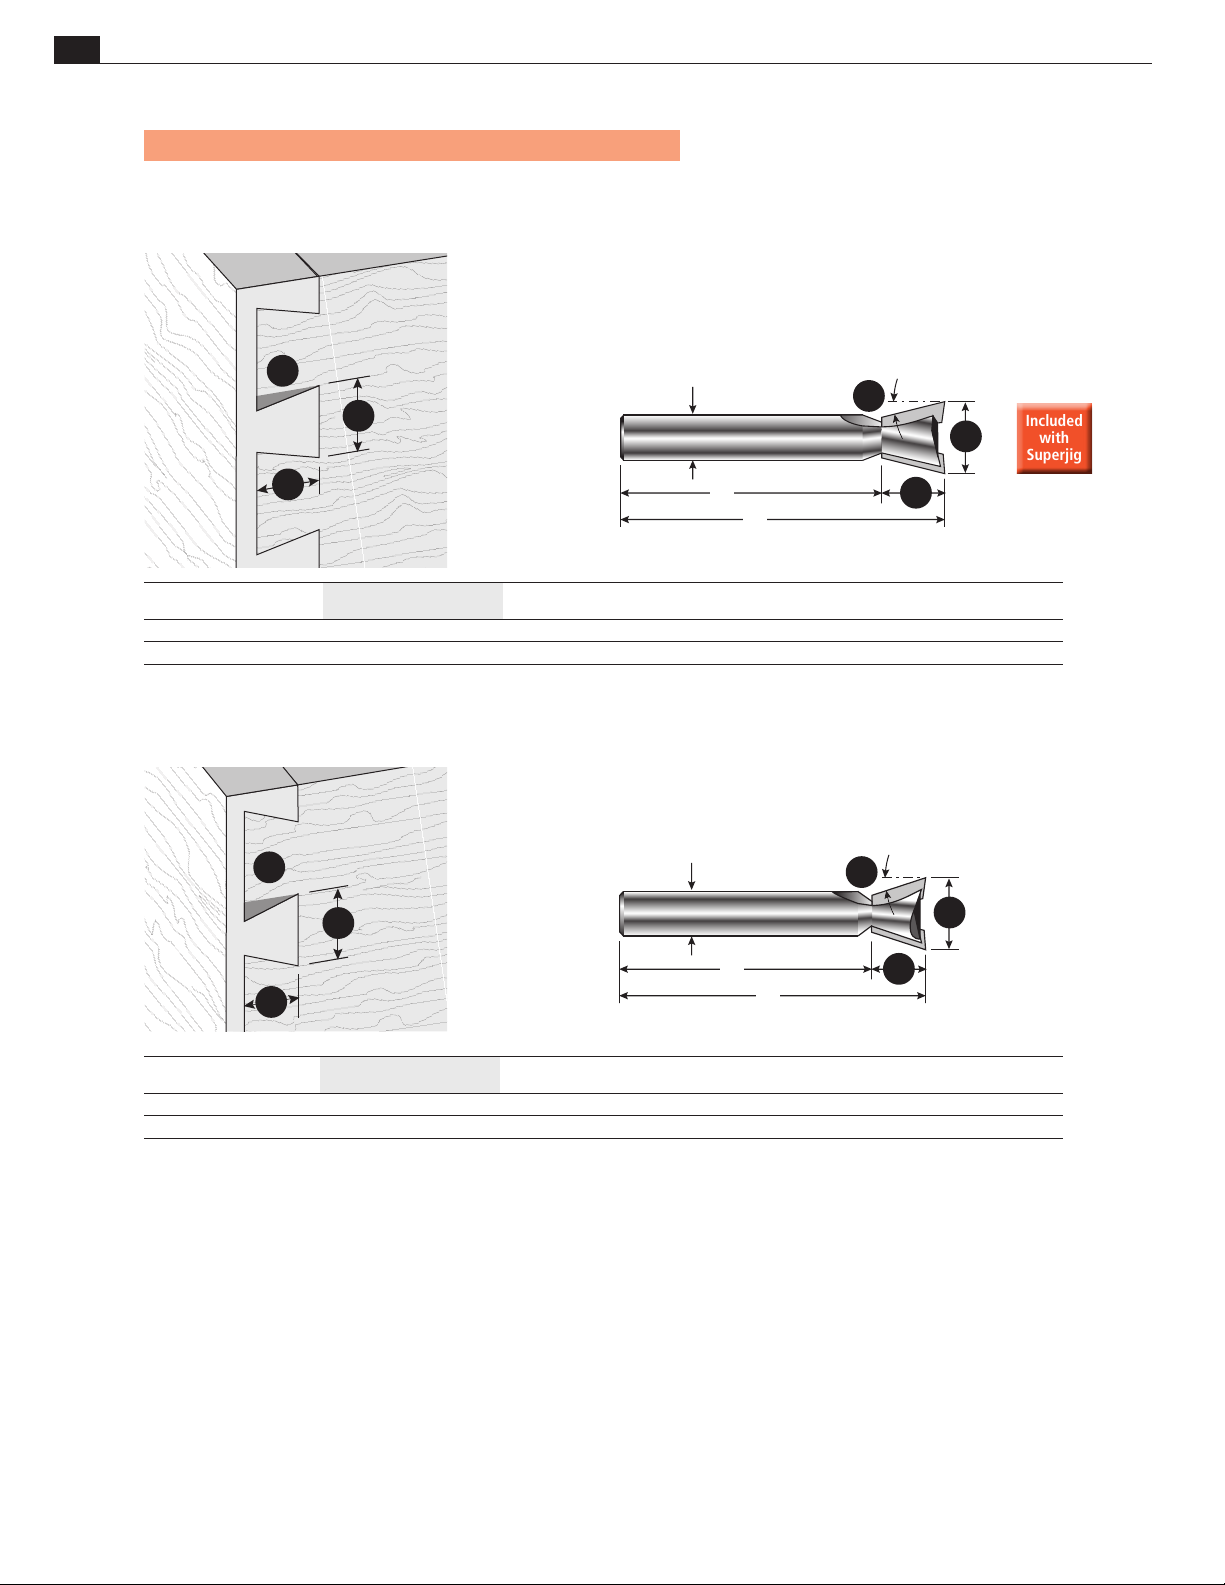
74
Included
with
Superjig
Included
with
Superjig
Appendix ii Sup er Jig -12-18-24 User Guide
Note: Bit and joint drawings are about actual size.
F
A
120-8
BIT SELECTION
C
F
A
B
D
B
E
A B C D E F Guidebush
Bits Overall Diameter Working Depth Shank Diameters Shank Length Overall Length Angle Diameter
HB Variable HB 1-Pass
No. 120-8* 1/2" [12,7] ~7/16" [11,0] ~9/32"[7,1mm] 8mm 1-3/4" [45,0] 2-1/4" [57] 14° e7 or 711C ~7/16" [11,1]
F
A
128-8
C
D
B
E
F
A
B
A B C D E F Guidebush
Bits Overall Diameter Working Depth Shank Diameters Shank Length Overall Length Angle Diameter
HB Variable HB 1-Pass
No. 128-8 1/2" [12,7] ~3/8" [9,5] 7/32"[5,5] 8mm 1-3/4" [45,0] 2-1/8" [54,0] 18° e7 or 711C ~7/16" [11,1]
Numbers in brackets are millimeters * Bits 80-8, 120-8, and 140-8 come standard with Leigh Super Jigs
Page 81
SUPERJIG - Appendix III
Jig Parts
See parts list and drawing on the following pages.
When ordering parts, please quote the jig model, serial number, part number, part description and quantity
required. Pay particular attention to the scale measurement, and let us know if yours is inch or metric.
75
Page 82
76
Appendix III S u p er Ji g-12-18-24 User Guide
How to Order Parts
Order directly from Leigh by calling toll free 800-663-8932, or if you’re outside North America contact
your national distributor. Have your jig information ready — You’ll need the jig model, serial number,
part number, part description and quantity required.
to determine left hand and right hand scales.
PART DESCRIPTION QUANTITY PART NO. SUPER 12 SUPER 18 SUPER 24
Super Jig Front Body Extrusion
Super Jig Rear Body Extrusion
Fingers
Finger Nuts (Threaded)
Finger Washers
Finger Wedges
8/32 x 7.35mm Finger Screws
R.H. Inch Scale Assembly, complete (R.H. in H.B. Tail Mode)
or R.H. Metric Scale Assembly, complete (R.H. in H.B. Tail Mode)
L.H. Inch Scale Assembly, complete (L.H. in H.B. Tail Mode)
L.H. Metric Scale Assembly, complete (L.H. in H.B. Tail Mode)
or
SJ End Housing R.H.
SJ End Housing L.H.
SJ Support Bracket R.H.
SJ Support Bracket L.H.
Scale Block R.H. (RH in HB Tail Mode)
Scale Block L.H. (LH in HB Tail Mode)
SJ Non-Slip Self Adhesive Strips
SJ Front Side Stops
SJ Rear Side Stops
SJ Spacer
Clamp Tube Extrusion - Front
Clamp Tube Extrusion - Rear
Clamp Tube End Plugs
Screwdriver
1" Aluminum Finger Bar
Plastic Bridge Extrusions
Nylon Depth Rod
Support Bracket Knobs
Clamp Bar Springs
Scale Thumb Screws
Scale Thumb Screw Washers
T-Bolts
End Housing Screws
5/16"x18 Hex Nuts
5/16" SAE Flat Washers
SJ Hold Down Screws #10 x 1"
SJ User Guide
SJ Instructional Pull Out
Cam Clamps
Cam Nuts 5/16-18
SJ Instructional DVD
# 80-8 1/2" Dovetail Bit
# 140-8 5/16" Straight Bit
# 120-8 Dovetail Bit
1/2" to 8mm Collet Reducer
e7 Oval Guide Bush & Nut
Pin Wrench
Note: Place the finger assembly in half-blind mode
1 8012 8018 8024
1 8112 8118 8124
see model 7200 Quantity 13 Quantity 16 Quantity 19
see model 7210 Quantity 15 Quantity 18 Quantity 21
see model 7215 Quantity 15 Quantity 18 Quantity 21
see model 7220 Quantity 15 Quantity 18 Quantity 21
see model 7225R Quantity 15 Quantity 18 Quantity 21
1 7230
1 7230M
1 7235
1 7235M
1 8005
1 8010
1 8050
1 8060
1 7230
1 7235
4 8712 8718 8724
2 8160
2 8170
1 8180
1 8212 8218 8224
1 8312 8318 8324
4 7115
1 550
1 8412 8418 8424
3 8512 8518 8524
1 8612 8618 8624
2 7025
4 311
2 7250
2 7255
4 7100
12 7145
4 300
4 283
4
1 8200
1 8210
4 7125
4 7120
1 8250
1 80-8
1 140-8
1 120-8
1 172-8
1 e7-Bush
1 730V
8145
JIG PARTS LIST
Page 83
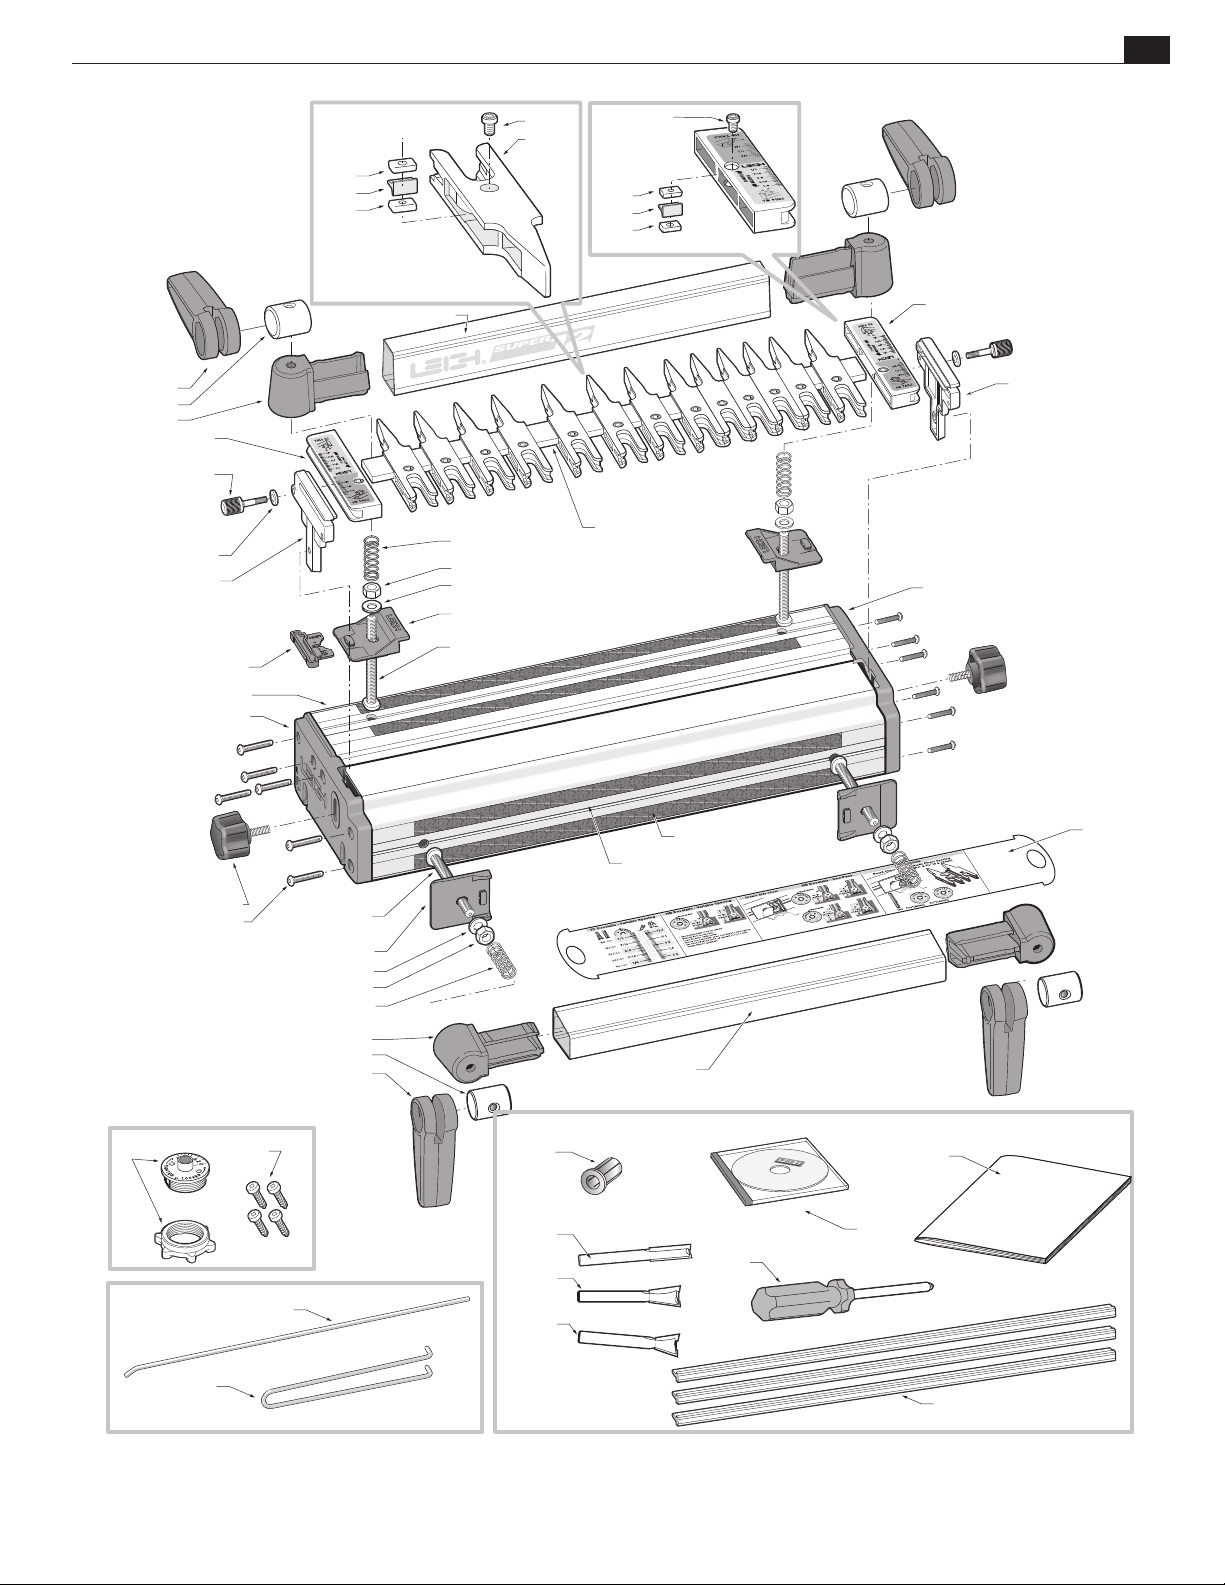
JIG PARTS LIST
Appendix IIISu p er Jig -12-18-24 User Guide
77
7125
7120
7115
7235
7235M
7250
7255
8060
8180
8112/ 8118/ 8124
8010
7215
7220
7210
(Threaded Nut)
8312/ 8318/ 8324
311
300
283
8170
7100
7225R
7200
7225R
7215
7220
7210
(Threaded Nut)
8412/ 8418/ 8424
7230
7230M
8005
8050
e7
8612/ 8618/ 8624
730V
7025
7145
8145
7100
8160
283
300
311
7115
7120
7125
172-8
140-8
80-8
120-8
8012/ 8018/ 8024
8212/ 8218/ 8224
8712/ 8718/ 8724
550
8210
8200
8250
8512/ 8518/ 8524
NOTE: When ordering parts, please quote the jig model, serial number, part number, part description and quantity required. Pay
particular attention to the scale measurement, inch or metric.
Page 84
78
Appendix III S u p er Ji g-12-18-24 User Guide
JIG PARTS LIST
Page 85
79
SUPERJIG - Appendix IV
Customer Support
Our Commitment to You Leigh Industries takes pride in its commitment to providing excellence in customer service and support. This
user guide is designed to provide you with the answers to any questions you have. However, if you require assistance, please feel free to
contact our technical support staff or a distributor listed below.
Manufacturer: Canada/USA
Email can be useful, but
TEL/FAX
Customer Service
and Technical Support
800-663-8932
604-464-2700 (Tel.)
604 464-7404 (Fax.)
(Canada/USA)
EMAIL/WEB
Customer Service
Technical Support
Website
www.leighjigs.com
NOTE:
technical queries usually raise
queries from us. A phone call is the
quickest and most convenient way
to get queries answered, either
directly to Leigh (toll free in N.
America) or to your national distribu-
–Thanks!
tor.
MAILING ADDRESS
Leigh Industries Ltd.
P.O. Box 357
Port Coquitlam, B.C.
Canada V3C 4K6
LOCATION
Leigh Industries Ltd.
1615 Industrial Ave.
Port Coquitlam, B.C.
Canada V3C 6M9
Distributors
AUSTRALIA & NEW ZEALAND
Carba-Tec Pty. ltd.
128 Ingleston Rd., Wakerley, Qld., 4154
Australia
Tel: (07) 3390 5888
Fax: (07) 3890 5280
Order: 180 658 111
Email: [email protected]
Web: www.carbatec.com.au
CHINA
Harvey Industries Co., Ltd.
68-10 Suyuan Avenue
Jiangning District Nanjing 211100, China
Tel: (0)86 5792 8869 / 5792 8021
Fax: (0)86 5792 8826
Email: [email protected]
Website: www.harveyworks.cn
FRANCE
Ets Bordet
23 Rue Traversiere
93556 Montreuil Cedex, France
Tel: 01 48 58 28 39
Fax: 01 48 58 48 58
Email: [email protected]
Web: www.bordet.fr/pages/
GERMANY, AUSTRIA & SWITZERLAND
Hacker GMBH
Holzbearbeitungsmaschinen
Traberhofstraße 103 D-83026 Rosenheim,
Deutschland
Tel: 08031 269650
Fax: 08031 68221
Email: [email protected]
Web: www.leigh.de
ITALY
Ferrari Macchine Legno SRL
Via Gallarata 74/76/78
20019 Settimo M.se (MI) Italy
Tel: 39 02 335 010 95
Fax: 39 02 335 005 27
Email: [email protected]
Web: www.ferrarimacchine.com
JAPAN
Off Corporation Inc.
323-1 Yanbara, Shimizu-ku, Shizuoka-shi
Shizuoka-ken, Japan 424-0002
Tel: 81-054-367-6511
Fax: 81-054-367-6515
Email: [email protected]
Web: www.off.co.jp
KOREA
Leigh Korea
1st Floor, Yongyu Building, 25-3,
Neung Pyung-Ri, Opo-Eup, Kwangju-Si,
Kyunggi-do, Korea
Tel: 82 (0) 70-8252-0988
Fax: 82 (0) 31-765-5602
Email: [email protected]
Web: www.htools.co.kr
RUSSIA
Unicom Ltd.
Nikitskij Boulevard 12
Moscow, 119019, Russia
Tel: 7 (495) 690 0454
Email: [email protected] (Russia)
Email: [email protected] (Ukraine)
Web: www.leighjigs.ru (Russia)
Web: www.leighjigs.ua (Ukraine)
SOUTH AFRICA
Hardware Centre Group
Post: PO Box 4059, 2125
Randburg, South Africa
Tel: (011) 791-0844/46
Fax: (011) 791-0850
Email: [email protected]
Web: www.hardwarecentre.co.za
SWEDEN
Toolbox Sweden AB
Bruksgatan 3, S-597 30
Atvidaberg, Sweden
Tel: 46 120 854 50
Fax: 46 120 854 69
Email: [email protected]
Web: www.toolbox.se
UNITED KINGDOM & IRELAND
Axminster Power Tool Centre Ltd.
Unit 10, Weycroft Avenue
Axminster, Devon
EX13 5PH United Kingdom
Tel: 03332 406406
Email: [email protected]
Web: axminster.co.uk/leigh
© 2007 Leigh Industries Ltd. All rights reserved. No part of this publication may be reproduced, stored in a retrieval system, or transmitted in
any form or by any means, electronic, mechanical, recording, or otherwise, without the prior written permission of Leigh Industries Ltd. 03/2015
Printed in Canada
Page 86
Joining Tradition with Today
Leigh Router Joinery Jigs
Printed in Canada
 Loading...