

Page 1
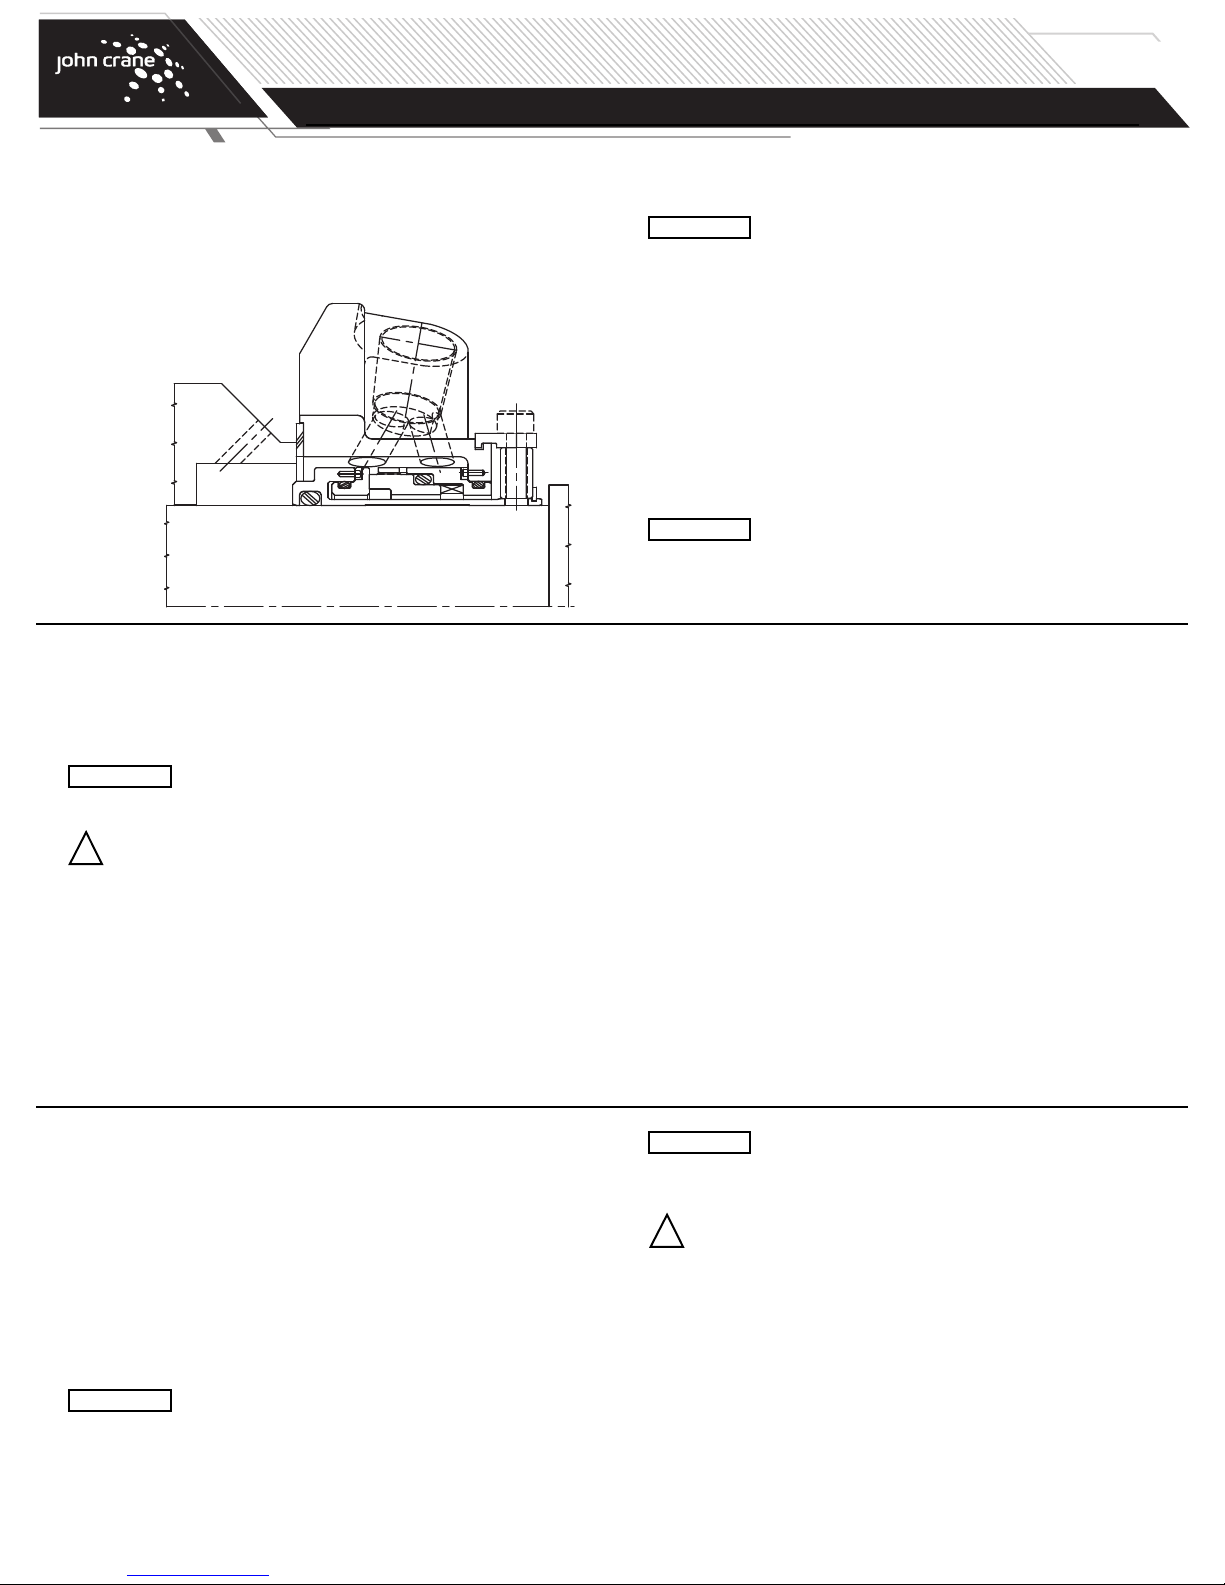
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Foreword
These instructions are provided to familiarize the user with the seal and its
designated use. The instructions must be read and applied whenever work
is done on the seal, and must be kept available for future reference.
PAGE
1
Installation, Operation & Maintenance Instructions
ATTENTION
If the seal is to be used for an application other than that originally
intended or outside the recommended performance limits, John Crane
must be contacted before its installation and use.
Any warranty may be affected by improper handling, installation, or use
of this seal. Contact John Crane for information as to exclusive product
warranty and limitations of liability.
If questions or problems arise, contact your local John Crane representative.
or the original equipment manufacturer, as appropriate.
ATTENTION
These instructions are for the installation and operation of
a seal as used in rotating equipment and will help to avoid
danger and increase reliability. The information required
may change with other types of equipment or installation
arrangements. These instructions must be read in
conjunction with the instruction manuals for both the
pump and any ancillary equipment.
John Crane mechanical seals are precision products and
must be handled appropriately. Take particular care to
avoid damage to lapped sealing faces and to flexible
sealing rings. Do not excessively compress the seal
before or during installation.
Safety Instructions
1. The following designations are used in the installation instructions to
highlight instructions of particular importance.
NOTE: Refers to special information on how to install or
Refers to special information or instructions directed
ATTENTION
Refers to mandatory instructions designed to
!
2. Installation, removal, and maintenance of the seal must be carried out
only by qualified personnel who have read and understood these
installation instructions.
3. The seal is designed exclusively for sealing rotating shafts. The
manufacturer cannot be held liable for use of the seal for purposes
other than this.
4. The seal must only be used in technically perfect condition, and
must be operated within the recommended performance limits in
accordance with its designated use set out in these installation
instructions.
operate the seal most efficiently.
towards the prevention of damage to the seal or its
surroundings.
prevent personal injury or extensive damage to the
seal or its surroundings.
Before Starting the Equipment
1. Check the pump at the coupling for proper alignment of the driver
or motor.
2. Ensure that the gland plate nuts/bolts are securely tightened
according to the pump manual instructions, and that all screws
are securely fastened.
3. Complete the assembly of the pump, and turn the shaft (by hand if
possible) to ensure free rotation.
4. Consult all available equipment operating instructions to check for
correctness of all piping and connections, particularly regarding seal
recirculation/flush, heating or cooling requirements, and services
external to the seal.
This mechanical seal is designed to operate in a liquid
ATTENTION
5. Check that the seal chamber fluid lines are open and free of any
obstruction, and ensure that the seal chamber is properly vented
and filled with liquid — refer to the pump instruction manual.
so the heat energy it creates is adequately removed.
Therefore, the following check should be carried out
not only after seal installation, but also after any
period of equipment inactivity.
5. If the pumped fluid is hazardous or toxic, appropriate precautions
must be taken to ensure that any seal leakage is adequately
contained. Further information on sealing hazardous or toxic fluids
should be obtained from John Crane prior to seal installation.
6. Fluorocarbon components should never be burned or incinerated
as the fumes and residues are highly toxic. If fluorocarbons are
accidentally heated above 400˚C/750˚F, they can decompose.
Protective gloves should be worn as hydrofluoric acid may be present.
7. PTFE components should never be burned or incinerated as the
fumes are highly toxic.
ATTENTION
!
WARNING: Seal installation should be handled only by qualified
Dry running — often indicated by a squealing noise from
the seal area — will cause overheating and scoring or
other damage to the sealing surfaces, resulting in
excessive leakage or a much shortened seal life.
Before startup, ensure that all personnel and
assembly equipment have been moved to a safe
distance so there is no contact with rotating parts
on the pump, seal, coupling, or motor.
personnel. If questions arise, contact the local
John Crane representative. Improper use and/or
installation of this product could result in injury to
the person and/or harmful emissions to
the environment, and may affect any warranty
on the product. Please contact the company for
information as to exclusive product warranty
and limitations of liability.
Page 2
63
SHAFT OR SLEEVE
0.040 LG. X 20˚ CHAM.
BORE
0
D +0.000"
- 0.002"
63
0.040"
20˚
MOVE SHAFT IN AXIAL DIRECTION
BY HAND. NOTE MEASUREMENT
ON DIAL INDICATOR
MOUNT
DIAL INDICATOR
ON SHAFT
TURN SHAFT BY HAND AND NOTE
MEASUREMENT ON DIAL INDICATOR
MOUNT
DIAL INDICATOR
ON SHAFT
TURN SHAFT BY HAND AND NOTE
MEASUREMENT ON DIAL INDICATOR
MOUNT
DIAL INDICATOR
ON SEAL CHAMBER
F
ACE
1
5 43 12 8
14
13
1
1
9
7
15
10
6 2
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Installation, Operation & Maintenance Instructions
PAGE
2
General Instructions
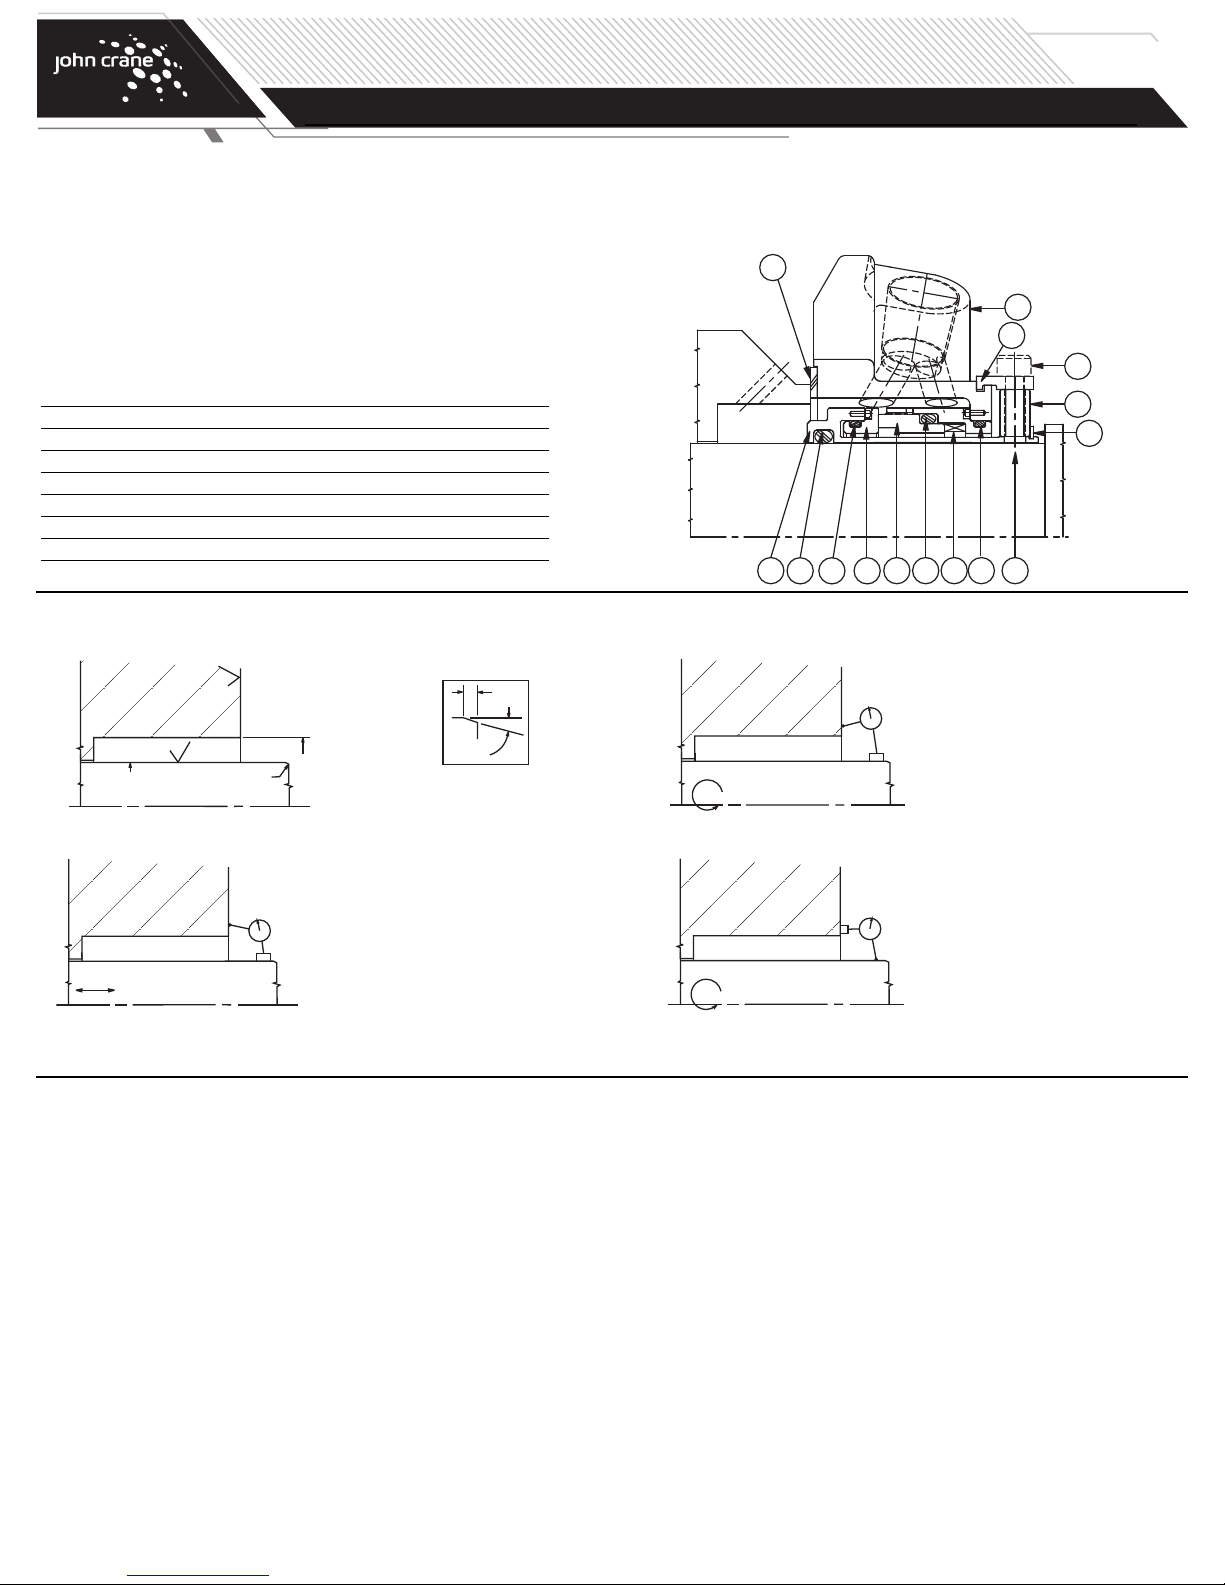
1. Study the engineering layout drawing to confirm the proper seal
arrangement for the pump being used. Types 5610V and 5610VQ seals
are designed for versatility and can be assembled in various ways.
The following instructions describe the standard configurations.
2. To assure satisfactory operation, handle the seal with care. Take
particular caution to see that the lapped sealing faces are not
scratched or damaged.
Part Name
1 Mating Ring 7 Collar 13 Gasket
2 O-ring 8 Set Screws 14 Snap Ring
3 Primary Ring 9 Spacers 15 O-ring
4 O-ring 10 Cap Screws
5 Sleeve Assembly 11 Gland Plate Assembly
6 O-ring 12 Spring
Preparing the Equipment
1. Check seal chamber dimensions and finishes:
Typical Type 5610V Single O-Ring Cartridge
eal Arrangement
S
3. Determine squareness of seal chamber face to shaft:
Rotating Mating Ring
Sizes to 3.000" = 0.005" FIM max.
3.000" and greater = 0.007" FIM max.
Rotating Seal Head
Sizes to 3.000" = 0.002" FIM max.
3.000" and greater = 0.003" FIM max.
2. Measure axial end play: Sizes to 3.000" = 0.003" FIM max.
3.000" and greater = 0.005" FIM
max.
4. Measure shaft runout:
Sizes to 3.000" = 0.002" FIM max.
3.000" and greater = 0.003" FIM
NOTE: If measured dimensions exceed those values given, correct the equipment to meet specifications prior to seal installation.
Type 5610V Single O-ring Cartridge Seal Assembly
Assemble the Type 5610V as follows, referring to the applicable
engineering layout drawing.
NOTE: These instructions apply to a rotating mating ring configuration.
The seal assembly and mating ring positions could be reversed
should an application require.
NOTE: Elastomeric O-rings can be damaged or destroyed if care is not
taken. Prior to assembly of O-ring into groove, make sure groove
is clean and free of foreign materials. Lubricate both groove and
O-ring prior to installation with light lube oil (SAE #10 or #20) or
silicone grease (such as Dow Corning compound #4). For ethylene
1. Place gland plate on table with gasket side facing up.
propylene elastomers, do not lubricate with petroleum products.
2. Install lubricated O-ring into outside diameter (OD) groove of mating
ring.
3. Stand sleeve on its base and slide mating ring over sleeve, align pins,
and press in place.
4. Install set screws in collar.
5. Loosely attach the spacers to the collar with cap screws.
6. Set the gland plate assembly gasket side down on table. Install
collar on gland plate assembly and engage spacers into groove,
aligning spacers with pipe taps of gland plate. Uniformly finger
tighten the cap screws.
7. Install lubricated O-ring into OD groove of retainer.
8. Place spring inside retainer.
9. Insert O-ring in retainer, ensuring that the O-ring is past the drive
slots.
10. Align ears on primary ring with slots on the retainer and press into
bore of retainer. Make sure primary ring is engaged into slots and
moves freely.
11. Place gland plate onto table with gasket side up.
12. Insert seal assembly in gland plate, align pins, and press in place.
Turn gland plate over and confirm that retainer is flush with end of
gland plate.
13. Clean faces of primary and mating rings with denatured alcohol
and a lint-free cloth.
14. Making sure seal face does not fall out, slide gland plate subassembly over sleeve until faces touch.
Page 3
SLOT
WIDTH
M
N
D1
D3
D4
*MIN. TURN DIAM.
L12
L23
L39L91 MIN.
BOX DEPTH
L92
L90 MIN. NEAREST OBSTRUCTION
D26
L
56
L12
D1
D3
L23
L39L91 MIN.
BOX DEPTH
L92
L90 MIN. NEAREST OBSTRUCTION
D26
L56
D4
*MIN. TURN DIAM.
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Type 5610V Single O-ring Cartridge Seal Assembly (continued)
15. Carefully rotate the gland plate until through holes in sleeve are lined
up with the collar set screws.
16. Carefully press down on gland plate and install snap ring over the end
of sleeve. This sets the axial spacing of the cartridge. Do not over-
compress gland plate or this may damage the seal.
17. Tighten set screws until they start to enter the sleeve ID.
18. Uniformly tighten cap screws on spacers.
19. Install gasket and sleeve O-ring. Apply a small amount of compatible
adhesive to gasket to hold it in place.
20. Pressure test according to John Crane standard QA-5-0568.
21. Plug pipe taps with plastic plugs.
PAGE
3
Installation, Operation & Maintenance Instructions
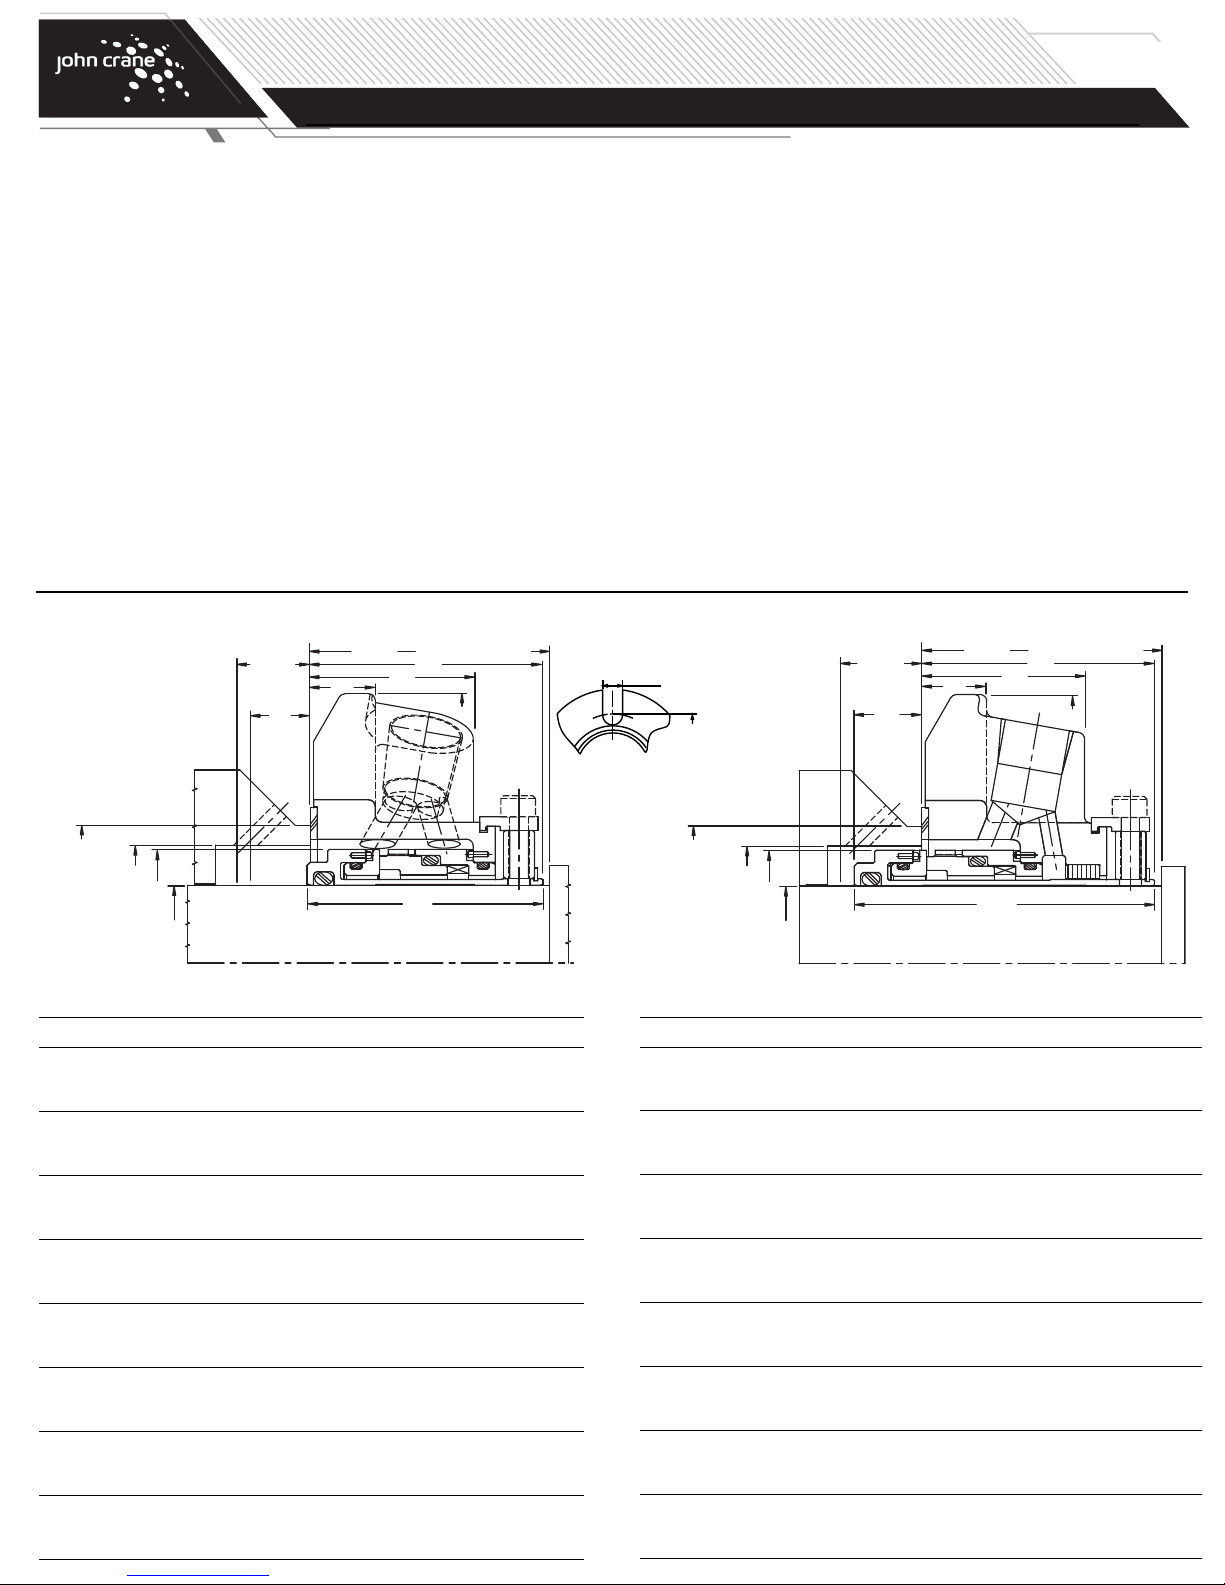
Typical Type 5610V Installation Dimensions
Type 5610V Single Cartridge Dimensional Data (inches)
Seal D4
Size/D1 D2 Min. Max. D26 L12 L23 L39 L56 L90 L91 L92 M N
1.000 1.375 1.445 1.889 4.000 1.989 1.353 1.954 0.531 2.000 0.160 0.035 0.525 2.805
1.125 1.500 N/A 2.015 4.125 2.062 1.446 2.062 0.531 2.125 0.125 N/A 0.525 2.933
1.250 1.625 N/A 2.294 4.250 2.062 1.446 2.062 0.531 2.125 0.125 N/A 0.525 3.213
1.375 1.750 N/A 2.421 4.375 2.062 1.446 2.062 0.531 2.125 0.125 N/A 0.525 3.338
1.500 1.937 2.007 2.680 4.875 2.156 1.487 2.125 0.593 2.187 0.156 0.031 0.525 3.599
1.625 2.062 2.132 2.812 5.000 2.156 1.487 2.125 0.593 2.187 0.156 0.031 0.562 3.766
1.750 2.170 2.240 2.918 5.250 2.156 1.487 2.125 0.593 2.187 0.156 0.031 0.562 3.875
1.875 2.312 2.382 2.918 5.250 2.156 1.487 2.125 0.593 2.187 0.156 0.031 0.562 3.875
2.000 2.437 2.507 3.015 5.500 2.375 1.601 2.312 1.063 2.375 0.187 0.062 0.562 4.000
2.125 2.562 2.632 3.360 5.859 2.375 1.601 2.312 1.593 2.375 0.187 0.062 0.687 4.469
2.250 2.687 2.757 3.485 6.500 2.375 1.601 2.312 0.593 2.375 0.187 0.062 0.687 4.566
2.375 2.812 2.882 3.610 6.500 2.484 1.717 2.466 0.625 2.528 0.143 0.018 0.687 4.719
2.500 3.062 N/A 3.891 6.750 2.484 1.717 2.562 0.625 2.625 0.125 N/A 0.687 5.000
2.625 3.312 N/A 4.062 6.750 2.500 1.625 2.500 0.625 2.562 0.125 N/A 0.687 5.170
2.750 3.312 N/A 4.062 6.750 2.500 1.625 2.500 0.625 2.562 0.125 N/A 0.687 5.170
2.875 3.375 N/A 4.186 7.000 2.500 1.725 2.500 0.625 2.562 0.125 N/A 0.687 5.312
3.000 3.625 N/A 4.469 7.750 2.500 1.787 2.562 0.685 2.625 0.125 N/A 0.812 5.720
3.125 3.750 3.853 4.600 7.875 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 5.845
3.250 3.750 3.853 4.600 7.437 2.562 1.593 2.510 N/A 2.635 0.177 0.052 0.812 5.845
3.375 4.000 4.125 4.850 8.125 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 6.095
3.500 4.125 4.250 4.975 8.250 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 6.220
3.625 4.218 4.343 5.100 8.375 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.687 6.250
3.750 4.343 4.468 5.199 8.750 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.687 6.770
3.875 4.468 4.593 5.375 8.750 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 6.636
4.000 4.593 4.718 5.500 9.000 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 6.761
4.125 4.718 4.843 5.625 9.000 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 6.886
4.250 4.843 4.968 5.750 9.250 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 7.011
4.500 5.093 5.218 6.000 9.500 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 7.261
4.750 5.343 5.468 6.313 10.375 2.562 1.593 2.562 N/A 2.687 0.125 N/A 0.812 7.574
5.000 5.843 5.968 7.260 12.000 2.953 1.749 3.043 N/A 3.168 0.125 N/A 0.812 10.000
5.250 6.093 6.218 7.510 12.250 2.953 1.749 3.043 N/A 3.168 0.125 N/A 0.812 10.250
5.500 6.343 6.468 8.000 12.687 2.953 1.749 3.043 N/A 3.168 0.125 N/A 0.937 10.500
Typical Type 5610VQ Installation Dimensions
Type 5610VQ Single Cartridge Dimensional Data (inches)
Seal D4
Size/D1 D3 Min. Max. D26 L12 L23 L39 L56 L90 L91 L92 M N
1.000 1.564 1.625 1.889 4.000 2.575 1.353 1.954 0.531 2.000 0.746 0.621 0.525 2.805
1.125 1.689 1.750 2.015 4.125 2.651 1.446 2.062 0.531 2.125 0.714 0.589 0.525 2.933
1.250 1.812 1.875 2.294 4.250 2.728 1.446 2.062 0.531 2.125 0.791 0.666 0.525 3.213
1.375 1.939 2.000 2.421 4.375 2.728 1.446 2.062 0.531 2.125 0.791 0.666 0.525 3.338
1.500 2.187 2.250 2.680 4.875 2.744 1.487 2.125 0.593 2.187 0.744 0.619 0.525 3.599
1.625 2.312 2.375 2.812 5.000 2.744 1.487 2.125 0.593 2.187 0.744 0.619 0.562 3.766
1.750 2.406 2.480 2.918 5.250 2.744 1.487 2.125 0.593 2.187 0.744 0.619 0.563 3.875
1.875 2.549 2.625 2.918 5.250 2.744 1.487 2.125 0.593 2.187 0.744 0.619 0.563 3.875
2.000 2.673 2.750 3.015 5.500 2.963 1.601 2.312 1.032 2.375 0.775 0.650 0.562 4.000
2.125 2.798 2.875 3.360 5.859 2.963 1.601 2.313 0.593 2.375 0.775 0.650 0.687 4.469
2.250 2.923 3.000 3.485 6.500 2.963 1.601 2.313 0.593 2.375 0.775 0.650 0.687 4.566
2.375 3.048 3.125 3.610 6.500 3.063 1.717 2.466 0.625 2.528 0.722 0.597 0.687 4.719
2.500 3.301 3.375 3.891 6.750 2.980 1.717 2.563 0.625 2.625 0.542 0.417 0.687 5.000
2.625 3.551 3.625 4.062 6.750 3.088 1.625 2.500 0.625 2.562 0.713 0.588 0.687 5.170
2.750 3.551 3.625 4.062 6.750 3.088 1.625 2.500 0.625 2.562 0.713 0.588 0.687 5.170
2.875 3.614 3.687 4.186 7.000 3.088 1.725 2.500 0.625 2.562 0.713 0.588 0.687 5.312
3.000 3.864 3.934 4.469 7.750 3.088 1.787 2.562 0.685 2.625 0.651 0.526 0.812 5.720
3.125 4.022 4.125 4.600 7.875 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 5.845
3.250 4.022 4.125 4.600 7.437 3.093 1.593 2.510 N/A 2.635 0.708 0.583 0.812 5.845
3.375 4.246 4.375 4.850 8.125 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 6.095
3.500 4.371 4.500 4.975 8.250 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 6.220
3.625 4.500 4.625 5.100 8.375 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.687 6.250
3.750 4.625 4.724 5.199 8.750 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.687 6.770
3.875 4.750 4.875 5.375 8.750 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 6.636
4.000 4.875 5.000 5.500 9.000 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 6.761
4.125 5.000 5.125 5.625 9.000 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 6.886
4.250 5.125 5.250 5.750 9.250 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 7.011
4.500 5.375 5.500 6.000 9.500 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 7.261
4.750 5.625 5.750 6.313 10.375 3.156 1.593 2.562 N/A 2.687 0.719 0.594 0.812 7.574
5.000 6.125 6.250 7.260 12.000 3.609 1.749 3.043 N/A 3.168 0.691 0.566 0.812 10.000
5.250 6.375 6.500 7.510 12.250 3.609 1.749 3.043 N/A 3.168 0.691 0.566 0.812 10.250
5.500 6.625 6.750 8.000 12.687 3.609 1.749 3.043 N/A 3.168 0.691 0.566 0.937 10.500
Page 4
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Installation, Operation & Maintenance Instructions
PAGE
4
Type 5610V Oversize Bore Single Cartridge
Dimensional Data (inches)
Seal D4 Min.
ize/D1 D2 Min. Max. D26 L12 L23 L39 L56 L90 L91 L92 M N Turn Diam.
S
1.375 1.750 2.875 3.023 5.375 2.062 1.446 2.062 0.625 2.125 0.250 0.125 0.562 4.062 3.268
1.750 2.170 3.500 3.925 6.500 2.156 1.487 2.125 0.656 2.187 0.250 0.125 0.687 5.093 3.885
1.875 2.312 3.625 3.734 6.500 2.156 1.316 1.954 0.485 2.017 0.327 0.202 0.687 5.093 *
.125 2.562 3.875 4.250 7.250 2.375 1.570 2.282 0.749 2.407 0.219 0.094 0.687 5.687 4.264
2
.500 3.062 4.750 5.078 8.000 2.484 1.697 2.407 0.749 2.625 0.204 0.079 0.687 6.062 5.139
2
2.625 3.312 4.625 4.740 8.000 2.500 1.619 2.329 0.578 2.454 0.296 0.171 0.687 6.062 **
2.750 3.312 4.750 4.875 8.000 2.500 1.697 2.407 0.656 2.532 0.218 0.093 0.687 6.062 5.139
*Seal cartridge is OD registered on the Turn Diam. of 4.125".
**Seal cartridge is OD registered on the Turn Diam. of 5.125".
Installing the Seal
1. Before starting the installation, read the following instructions carefully.
2. Remove the seal from its packaging, inspect for any damage and wipe
clean.
3. The equipment should be clean and meet the specifications noted in
the “Preparing the Equipment” section. Lubricate sleeve O-ring with
lubricant recommended in chart below. Lubricate shaft sparingly.
Lubricate gland plate bolts/nuts as required.
ELASTOMER LUBRICANT
Fluoroelastomer Vegetable Oil, Animal Oil, Mineral-Hydrocarbon Oils,
(i.e., Viton®) Soap Solution, Parker ‘Super-O-Lube,’ Silicone Grease
Ethylene Propylene Vegetable Oil, Polywater®, Soap Solution, Glycerine,
Propylene Glycol, Silicone Grease
Perfluoroelastomer Vegetable Oil, Animal Oil, Mineral-Hydrocarbon Oils
(i.e., Kalrez®)
NOTE: Always use a lubricant that is compatible with your machinery and product.
Use lubricant sparingly, only enough to install seal with ease.
Viton and Kalrez are registered trademarks of DuPont.
Polywater is a registered trademark of American Polyware Co.
Type 5610VQ Oversize Bore Single Cartridge
Dimensional Data (inches)
Seal D4 Min.
ize/D1 D3 Min. Max. D26 L12 L23 L39 L56 L90 L91 L92 M N Turn Diam.
S
1.375 1.939 2.875 3.023 5.375 2.062 1.446 2.062 0.625 2.125 0.791 0.666 0.562 4.062 3.268
1.750 2.406 3.500 3.925 6.500 2.156 1.487 2.125 0.656 2.187 0.744 0.619 0.687 5.093 3.885
1.875 2.549 3.625 3.734 6.500 2.156 1.316 1.954 0.485 2.017 0.915 0.790 0.687 5.093 *
.125 2.798 3.875 4.250 7.156 2.375 1.570 2.282 0.749 2.407 0.806 0.681 0.687 5.687 4.264
2
.500 3.301 4.750 5.078 8.000 2.484 1.697 2.407 0.656 2.532 0.698 0.573 0.687 6.062 5.000
2
2.625 3.551 4.625 4.740 8.000 3.088 1.619 2.329 0.578 2.454 0.884 0.759 0.687 6.062 **
2.750 3.551 4.750 4.875 8.000 2.500 1.697 2.407 0.656 2.532 0.806 0.681 0.687 6.062 5.139
*Seal cartridge is OD registered on the Turn Diam. of 4.125".
**Seal cartridge is OD registered on the Turn Diam. of 5.125".
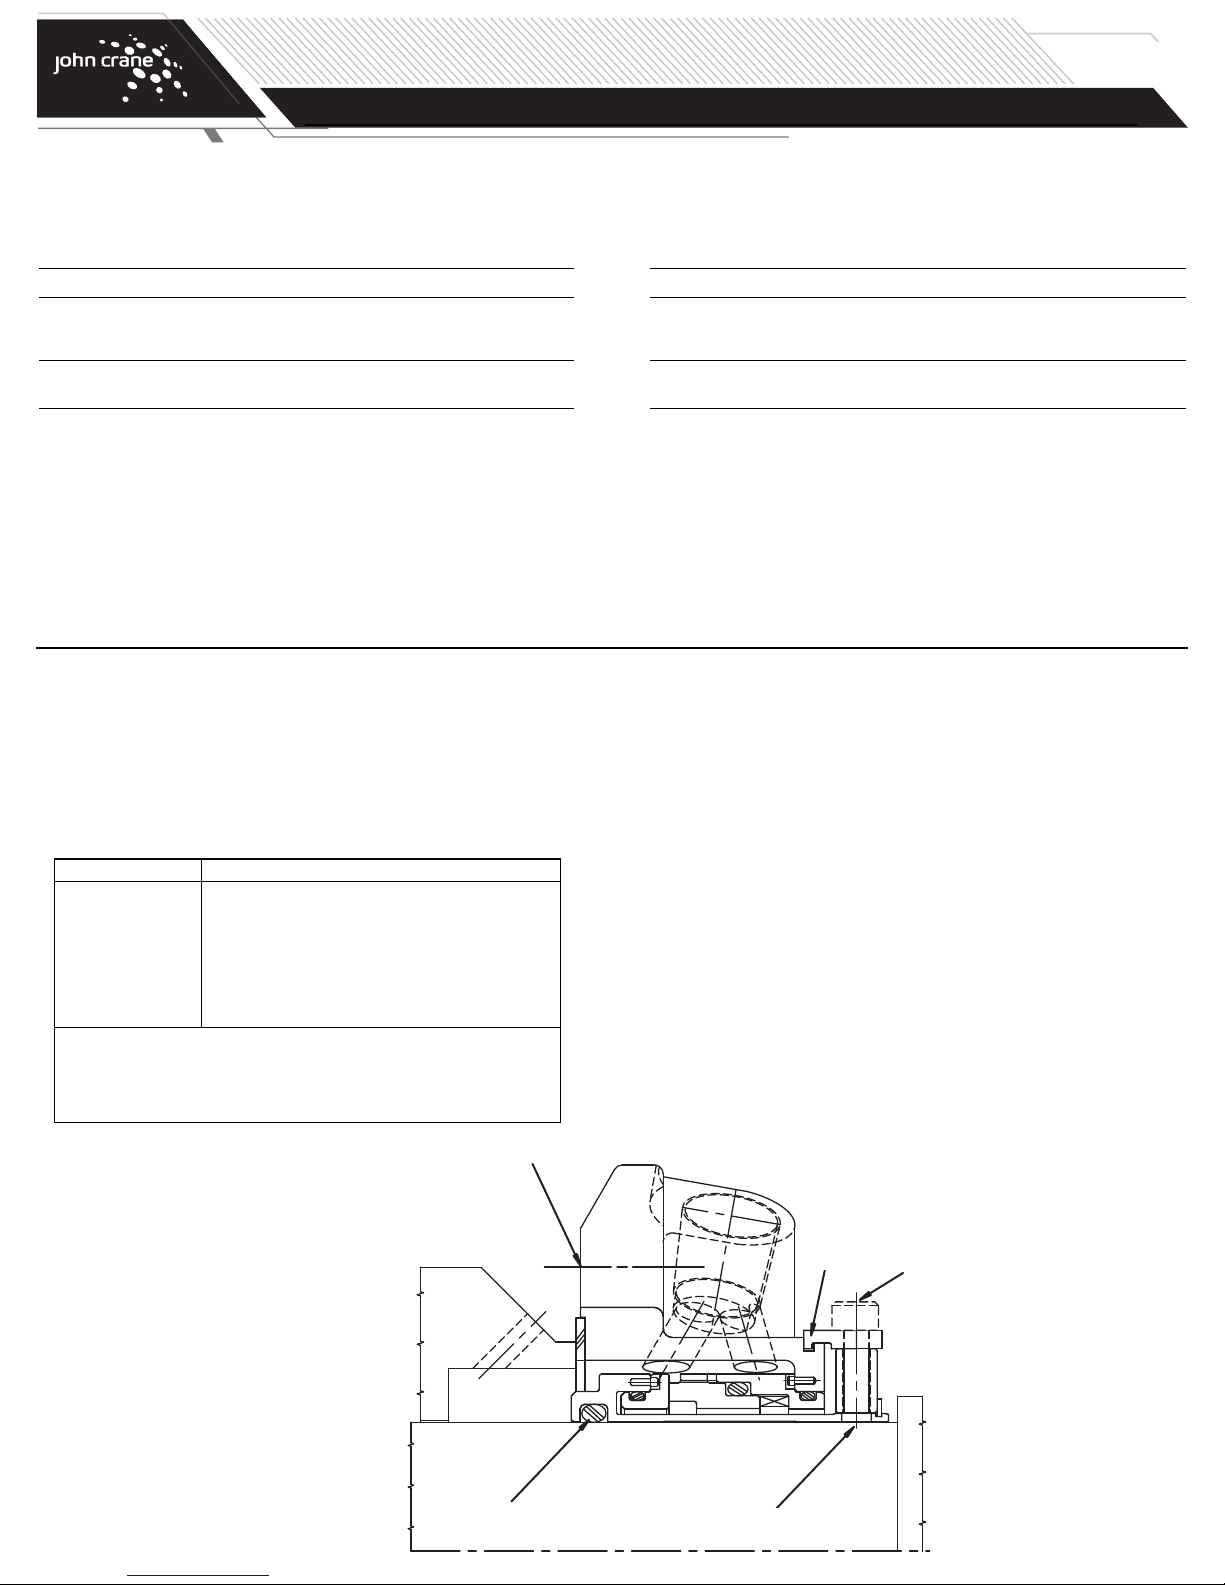
4. Make sure that gland plate gasket is properly positioned, and that
collar set screws do not extend past sleeve ID. Slide complete
cartridge seal assembly onto shaft. For ANSI pumps, position gland
plate so pipe connection #1 is at or near top dead center. For DIN
pumps, position gland plate so slot between pipe connections #2
and #3 is at or near top dead center. Slide cartridge onto studs (if
applicable) until gasket is flush against the face of seal chamber.
Hand tighten gland plate bolts/nuts.
5. Reassemble pump and make all necessary impeller adjustments.
6. Continue tightening gland plate bolts/nuts in an alternating pattern
until secure (1/4 turns, 180˚ apart), with gland plate and face of
pump seal chamber metal to metal. Do not over-stress or distort
gland plate.
7. Tighten collar set screws evenly (1/4 turns, 180˚ apart), securing
cartridge seal to shaft.
8. Remove spacers and save.
9. Make appropriate piping connections to seal assembly.
GLAND BOLTS
O-RING
SET SCREWS
SPACERS
CAP SCREWS
Page 5
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Installing the Seal (continued)
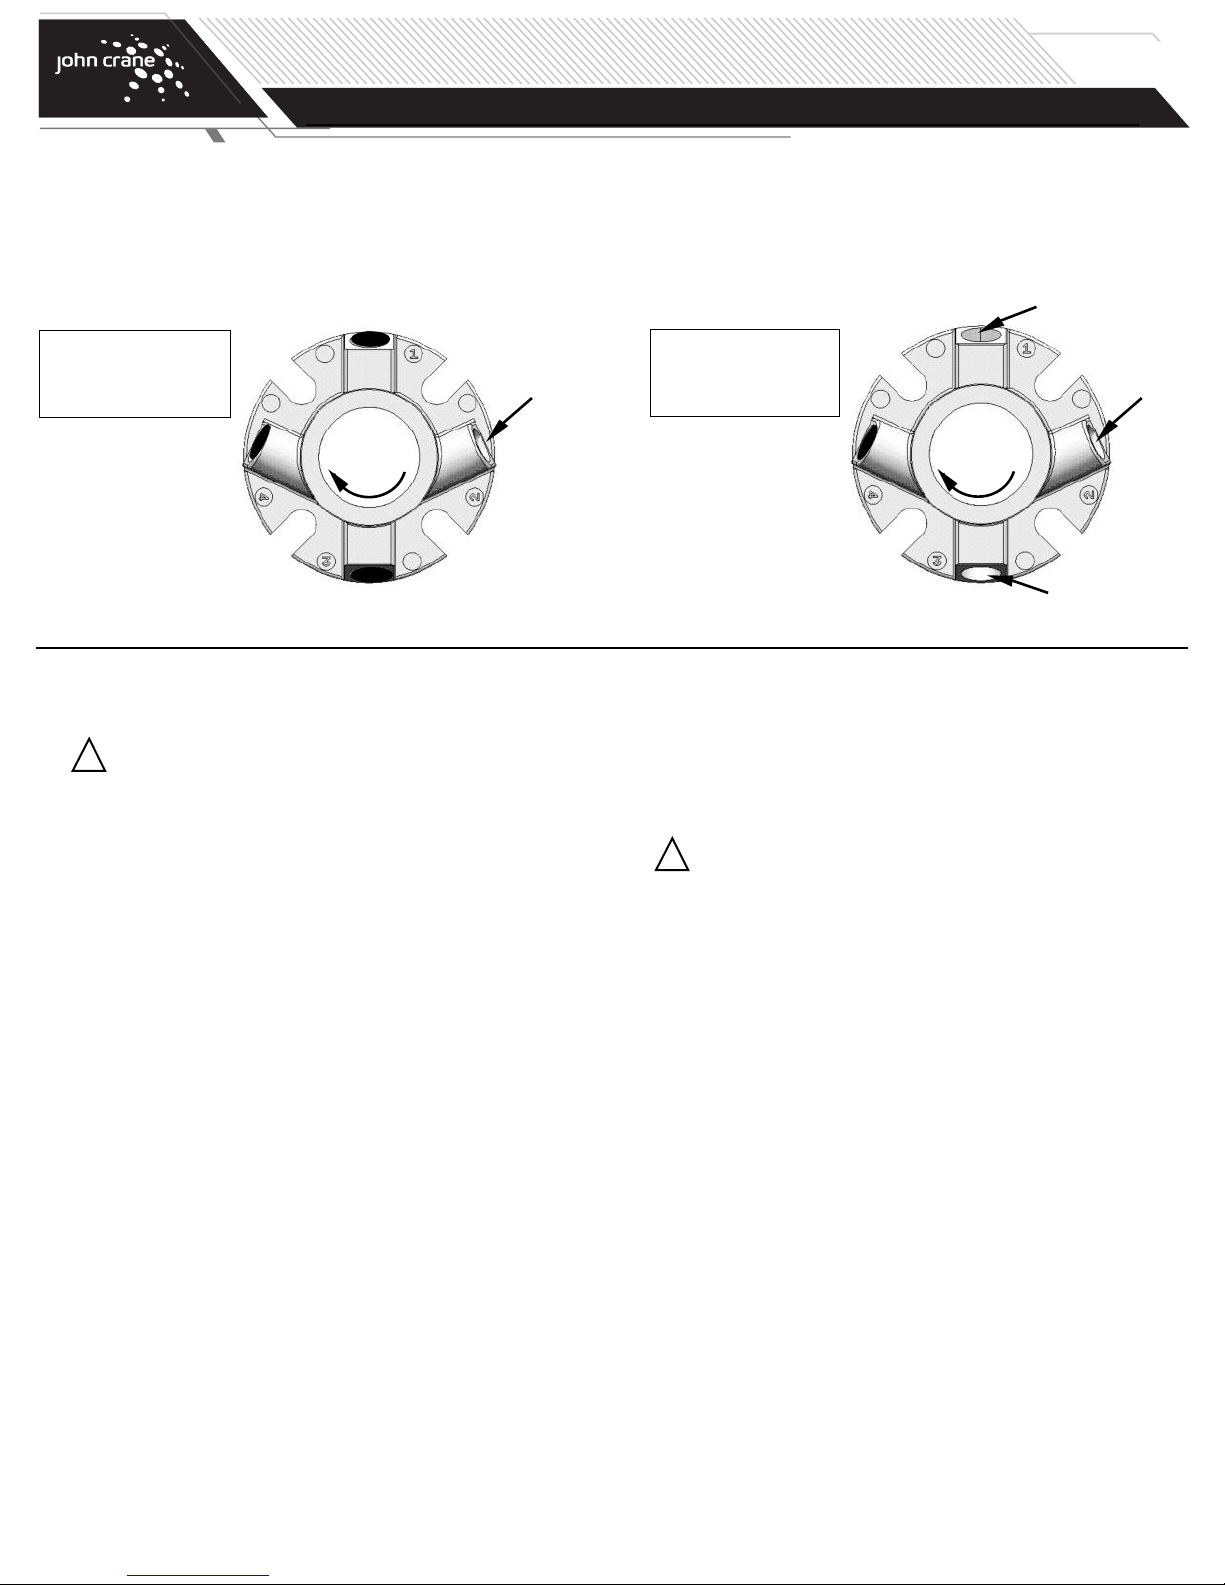
It is recommended that the seal cavity be vented through the pump’s lantern
ring connection located at top dead center. It is always recommended that a
flush injection be utilized. The flush should be piped into the seal gland to
ensure maximum efficiency.
PAGE
5
Installation, Operation & Maintenance Instructions
For DIN pumps rotate gland 135˚ CCW. Use port #2 as flush.
NOTE: For CCW (counter clockwise) rotation pumps,
consult John Crane engineering.
Quench “Q”
Port #1 - Not Drilled
Port #2 - Flush
Port #3 - Not Drilled
Port #4 - Not Drilled
Clockwise
Rotation
Type 5610V
Flush “F”
Decommissioning the Equipment
1. Ensure that the equipment is electrically isolated.
If the equipment has been used on toxic or hazardous
2. Ensure that the equipment is isolated by the appropriate valves.
fluids, ensure that the equipment is correctly decontami-
!
nated and made safe prior to commencing work.
Remember, fluid is often trapped during draining and
may exist outside the seal. The equipment instruction
manual should be consulted to check for any special precautions.
Check that the fluid is drained and pressure is fully released.
Port #1 - Quench
Port #2 - Flush
Port #3 - Drain
Port #4 - Not Drilled
Clockwise
Rotation
Type 5610VQ
Flush “F”
Drain “D”
Maintenance
No maintenance of a seal is possible while installed. Therefore, it is
recommended that a spare seal unit be held in stock to allow immediate
replacement of a removed seal.
It is recommended that used seals are returned to a John Crane service
location, as rebuilding to as-new specifications must be carried out by
qualified personnel.
It is the responsibility of the equipment user to ensure that any
parts being sent to a third party have appropriate safe
!
handling instructions externally attached to the package.
Quality Assurance
This seal has been assembled in accordance with John Crane quality
assurance standards and with proper maintenance and use will give safe
and reliable operation to the maximum recommended performance as
shown in any relevant approved John Crane publication.
Page 6
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Installation, Operation & Maintenance Instructions
PAGE
6
Ordering Information
1. Cartridge seal size = solid shaft or sleeve outside diameter (OD).
2. Select single (5610V) or single with quench (5610VQ) arrangement.
3. Determine whether standard or enlarged seal chamber configuration
is required.
4. Choose seal drawing number from chart below.
5. For other material combinations or size considerations, consult your
local John Crane representative.
Type 5610V/5610VQ Cartridge Drawing Numbers
Standard Bore Layouts
Seal Size 5610V 5610VQ
1.000 H-SP-1030362 H-SP-1030394
1.125 H-SP-1030363 H-SP-1030395
1.250 H-SP-1030364 H-SP-1030396
1.375 H-SP-1030365 H-SP-1030397
1.500 H-SP-1030366 H-SP-1030398
1.625 H-SP-1030367 H-SP-1030399
1.750 H-SP-1030368 H-SP-1030400
1.875 H-SP-1030369 H-SP-1030401
2.000 H-SP-1030370 H-SP-1030402
2.125 H-SP-1030371 H-SP-1030403
2.250 H-SP-1030371 H-SP-1030404
2.375 H-SP-1030373 H-SP-1030405
2.500 H-SP-1030374 H-SP-1030406
2.625 H-SP-1030375 H-SP-1030407
2.750 H-SP-1030376 H-SP-1030408
2.875 H-SP-1030377 H-SP-1030409
3.000 H-SP-1030378 H-SP-1030410
3.125 H-SP-1030379 H-SP-1030411
3.250 H-SP-1030380 H-SP-1030412
3.375 H-SP-1030381 H-SP-1030413
3.500 H-SP-1030382 H-SP-1030414
3.625 H-SP-1030383 H-SP-1030415
3.750 H-SP-1030384 H-SP-1030416
3.875 H-SP-1030385 H-SP-1030417
4.000 H-SP-1030386 H-SP-1030418
4.125 H-SP-1030387 H-SP-1030419
4.250 H-SP-1030388 H-SP-1030420
4.500 H-SP-1030389 H-SP-1030421
4.750 H-SP-1030390 H-SP-1030422
5.000 H-SP-1030391 H-SP-1030423
5.250 H-SP-1030392 H-SP-1030424
5.500 H-SP-1030393 H-SP-1030425
Materials of Construction - Standard
Primary Ring Carbon Graphite
Silicon Carbide (optional)
Nickel Binder Tungsten Carbide (optional)
Mating Ring Silicon Carbide
Nickel Binder Tungsten Carbide (optional)
Cartridge Hardware 316 Stainless Steel*
Secondary Seal Fluoroelastomer*
Operating Limits
Pressure: Sizes up to 3.000" — 21 bar g/300 psig max.
Sizes over 3.000" — 13 bar g/200 psig
Temperature: -29˚C to 204˚C/-20˚F to 400˚F
Speed: To 25 m/s/5,000 fpm
*Various options.
Type 5610V/5610VQ Cartridge Drawing
Numbers
Oversize Bore Layouts
Seal Size 5610V 5610VQ
1.375 H-SP-1032553 H-SP-1032554
1.750 H-SP-1032556 H-SP-1032557
1.875 H-SP-1032559 H-SP-1032560
2.125 H-SP-1032562 H-SP-1032563
2.500 H-SP-1032565 H-SP-1032566
2.625 H-SP-1032568 H-SP-1032569
2.750 H-SP-1032571 H-SP-1032572
Page 7
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Installation, Operation & Maintenance Instructions
PAGE
7
Page 8
TYPE 5610V/5610VQ
SINGLE O-RING CARTRIDGE SEAL
Installation, Operation & Maintenance Instructions
PAGE
8
North America
United States of America
Tel: 1-847-967-2400
Fax: 1-847-967-3915
If the products featured will be used in a potentially dangerous and/or hazardous process, your John Crane representative should be consulted prior to
their selection and use. In the interest of continuous development, John Crane Companies reserve the right to alter designs and specifications without
prior notice. It is dangerous to smoke while handling products made from PTFE. Old and new PTFE products must not be incinerated. ISO 9001 and
ISO14001 Certified, details available on request.
©2015 John Crane
Europe
United Kingdom
Tel: 44-1753-224000
Fax: 44-1753-224224
Revised 10/15 www.johncrane.com IOM-5610/5610VQ
Latin America
Brazil
Tel: 55-11-3371-2500
Fax: 55-11-3371-2599
Middle East & Africa
United Arab Emirates
Tel: 971-481-27800
Fax: 971-488-62830
Asia Pacific
Singapore
Tel: 65-6518-1800
Fax: 65-6518-1803
 Loading...