

Page 1
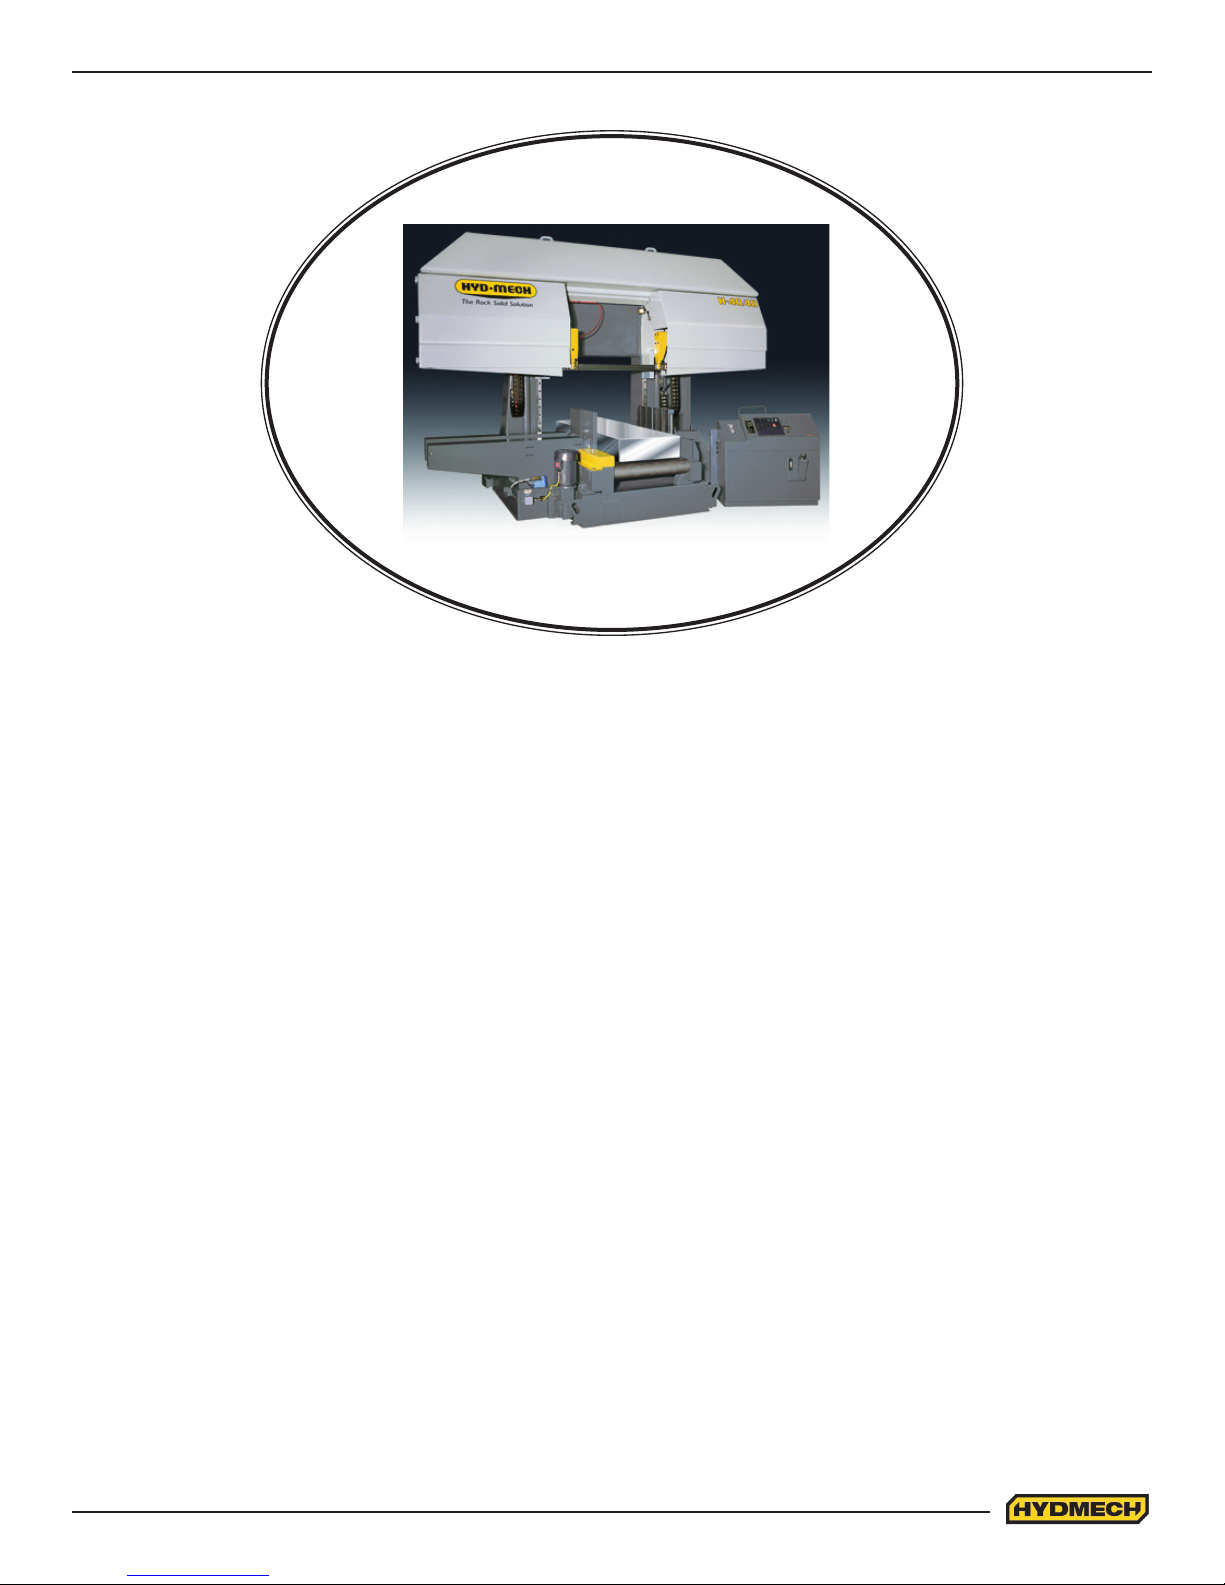
H4040, H4060, H4080
393139
THANK YOU,
On behalf of everyone at HYD·MECH Group Limited, we would like to thank and congratulate you on your decision to
purchase a HYD·MECH bandsaw.
Your new machine is now ready to play a key role in increasing the eciency of your operation, helping you to reduce cost
while boosting quality and productivity.
To ensure you are maximizing the power and versatility of your new HYD·MECH bandsaw, please take the time to
familiarize yourself and your employees with the correct operation and maintenance procedures as outlined in this
manual. Please keep this instruction manual for future reference in a known location and easily accessible to all users of
the device.
HYD·MECH oers a great variety of options, components, and features for its various models. Therefore, some of the
equipment described in this manual (various illustrations and drawings) may not be applicable to your particular machine.
The information and specications provided in this manual were accurate at the time of printing. HYD·MECH reserves the
right to discontinue or change specications or design at any time without notice and without incurring any obligation.
Thank you.
Hyd·Mech Group Limited
P.O. Box 1659, 1079 Parkinson Road
Woodstock, Ontario, N4S 0A9
Phone : (519) 539-6341
Service : 1-877-237-0914
Sales : 1-877-276-SAWS (7297)
Fax : (519) 539-5126
e-mail : [email protected]
PRINTED APRIL 2017
1
Page 2
TABLE OF CONTENTS
SECTION 0 - SAFETY INSTRUCTIONS
SUMMARY .......................................................................................................................................0.1
BASIC RULES ..................................................................................................................................0.3
RESPONSIBILITIES OF THE OWNER ............................................................................................0.3
RESPONSIBILITIES OF THE OPERATOR AND MAINTENANCE PERSONNEL ...........................0.4
SAFETY HAZARD LABELS .............................................................................................................0.6
SECTION 1 - INSTALLATION
SAFETY PRECAUTIONS .................................................................................................................1.1
LIFTING THE H-40 ...........................................................................................................................1.2
MACHINE LAYOUT ..........................................................................................................................1.3
H-40 INSTALLATION PROCEDURE ................................................................................................1.4
FOUNDATION, LEVELING AND ANCHORING ...............................................................................1.4
HYDRAULIC OIL AND CUTTING FLUID .........................................................................................1.6
WIRING CONNECTIONS .................................................................................................................1.6
SECTION 2 - OPERATING INSTRUCTIONS
BLADE BASICS................................................................................................................................2.1
VARIABLE SPEED CONTROL.........................................................................................................2.1
THE CONTROL PANEL ...................................................................................................................2.1
MANUAL OPERATION .....................................................................................................................2.1
HYDRAULIC FEED CONTROL ........................................................................................................2.6
CUTTING PARAMETERS CHART ...................................................................................................2.7
HEAD DOWN LIMIT SETTING .......................................................................................................2.13
GUIDE ARM POSITIONING ............................................................................................................2.14
COOLANT CONTROLS ..................................................................................................................2.15
SECTION 3 – MAINTENANCE
SAFETY DURING MAINTENANCE AND TROUBLESHOOTING ....................................................3.1
LOCK OUT PROCEDURE ...............................................................................................................3.1
BLADE CHANGE MODE PROCEDURE ..........................................................................................3.2
BLADE BRUSH ADJUSTMENT .......................................................................................................3.4
LUBRICATION ..................................................................................................................................3.5
HYDRAULIC MAINTENANCE ..........................................................................................................3.6
CLEANLINESS .................................................................................................................................3.6
TROUBLE SHOOTING GUIDE ........................................................................................................3.7
ELECTRICAL SCHEMATICS: SEE PDF ON ATTACHED CD .........................................................4.1
SECTION 4 - ELECTRICAL
i
Page 3
SECTION 5 - HYDRAULIC SYSTEM
HYDRAULIC SCHEMATICS & PLUMBING DIAGRAMS: SEE PDF ON ATTACHED CD ...............5.2
LIST OF H-40 HYDRAULIC COMPONENTS ...................................................................................5.2
SECTION 6 - MECHANICAL ASSEMBLIES
MECHANICAL ASSEMBLY DRAWINGS & PARTS LIST: SEE PDF ON ATTACHED CD ................6.1
SECTION 7 - OPTIONS
OPTIONAL ASSEMBLY DRAWINGS: SEE PDF ON ATTACHED CD .............................................7.1
BLADE DEVIATION MONITORING SYSTEM (K10) ........................................................................7.1
SECTION 8 - SPECIFICATIONS
H4040 SPECIFICATIONS ................................................................................................................8.1
H4060 SPECIFICATIONS ................................................................................................................8.2
H4080 SPECIFICATIONS ................................................................................................................8.3
LAYOUT DRAWING .........................................................................................................................8.4
SECTION 9 - WARRANTY
WARRANTY .....................................................................................................................................9.1
ii
Page 4
SECTION 0 - SAFETY INSTRUCTIONS
SUMMARY
All persons operating this machine must have read and understood all of the following sections of this Manual:
Section 0 SAFETY
Section 2 OPERATING INSTRUCTIONS
However, as a memory aid, the following is a summary of the Safety Section.
Put Safety First
Mandatory Information – What operators and maintenance people must have read and understood.
Signatures – Everyone involved with this machine must sign to conrm they have read and understood mandatory
information.
Basic Rules – only use this machine when
• It is in good working order.
• All safety equipment is in place and functional.
• Operations are in compliance with this manual.
• Materials are within designed specications and are non-hazardous.
Owner is responsible to
• Keep Manual accessible at the machine.
• Ensure only reliable, fully trained personnel work with the machine.
• Clearly dene responsibilities of all personnel working with the machine.
• Keep the machine in good working order.
Operator and Maintenance Personnel are responsible to:
• Keep all safety equipment in order, check its function at the beginning of each shift, and report any shortcomings.
• Shut down machine and report any faults or malfunctions that could impair safety.
• Understand and obey safety hazard labels.
• Not to wear un-restrained long hair, loose clothing or jewellery.
• Wear all required personal protective equipment.
• Not to wear gloves within 24 inches of moving blade.
• Maintain a clean working area and machine.
• Always use Lock-out when performing maintenance or repairs.
0.1
Page 5
FOREWORD
Put Safety First!
This Safety Section contains important information to help you work safely with your machine and describes the dangers
inherent to bandsaws. Some of these dangers are obvious, while others are less evident.
It really is important to PUT SAFETY FIRST. Make it a habit to consider the hazards associated with any action BEFORE
you do it. If you feel any uncertainty, stop and nd a safer approach to the action. If you’re still uncertain, ask for advice
from your supervisor.
The SAFETY FIRST approach is particularly necessary when you do something new, or dierent, and most people
instinctively recognize this, although impatience may still cause them to take unnecessary risks.
Danger also lurks in the routine task that we have done over and over. Here, familiarity, boredom, or tiredness may lull us
into unthinking, automatic repetition. Be alert for this, and when you feel it happening, stop and assess your
situation. Review the safety hazards associated with what you are doing. That should get your brain working again.
Certainly production is important, but if you think you’re too busy to put safety rst, think how much production you’ll lose if
you get hurt.
You owe it to yourself, your family, and your co-workers to PUT SAFETY FIRST.
Mandatory Information
All persons operating this machine must have read and understood all of the following sections of this Manual:
Section 0 SAFETY
Section 2 OPERATING INSTRUCTIONS
Personnel involved in installation and maintenance of the machine must have read and understood all sections of the
manual
Persons who have diculty reading, or for whom English is not their rst language, must receive particularly thorough
instruction.
Signatures
Everyone involved in operation of this machine must sign below to conrm that:
I have read and understood all parts of Section 0 – Safety, and Section 2 – Operating Instructions.
Name Date Signature
Everyone involved in the installation, inspection, maintenance, and repair of this machine must sign below to conrm that:
I have read and understood all parts of this Operation and Maintenance Manual.
Name Date Signature
0.2
Page 6
BASIC RULES
Intended Use
Exclusion of Misuse
Liability
Our machines are designed and built in line with the state of the art, and specically in accordance with
American National Standards Institute Standard B11.10 Safety Requirements for Metal Sawing Machines.
However, all machines may endanger the safety of their users and/or third parties, and be damaged,
or damage other property, if they are operated incorrectly, used beyond their specied capacity, or for
purposes other than those specied in this Manual.
Misuse includes, for example:
Sawing hazardous materials such as magnesium or lead.
Sawing work pieces which exceed the maximum workload appearing in the Specications.
Operating the machine without all original safety equipment and guards.
The machine may only be operated:
When it is in good working order, and
When the operator has read and understood the Safety and Operating Instructions Sections of the
Manual, and
When all operations and procedures are in compliance with this Manual.
Hyd-Mech Group cannot accept any liability for personal injury or property damage due to operator errors
or non-compliance with the Safety and Operating Instructions contained in this Manual.
RESPONSIBILITIES OF THE OWNER
Organization of work
This Operation and Maintenance Manual must always be kept near the machine so that it is accessible to
all concerned.
The general, statutory and other legal regulations on accident prevention and environmental protection
must also be observed, in addition to the Manual material. The operators and maintenance personnel
must be instructed accordingly. This obligation also includes the handling of dangerous substances and
the provision and use of personal protective equipment.
Choice and qualication of personnel
Ensure that work on the machine is only carried out by reliable persons who have been appropriately
trained for such work.
Training
Everyone working on or with the machine must be properly trained with regard to the correct use of the
machine, the correct use of safety equipment, the foreseeable dangers that may arise during operation of
the machine, and the safety precautions to be taken.
In addition, the personnel must be instructed to check all safety devices at regular intervals.
0.3
Page 7
Dene responsibilities
Clearly dene exactly who is responsible for operating, setting-up, servicing and repairing the machine.
Dene the responsibilities of the machine operator and authorize him to refuse any instructions by third
parties if they run contrary to the machine’s safety.
Persons being trained on the machine may only work on or with the machine under the constant
supervision of an experienced operator. Observe the minimum age limits required by law.
Condition of Machine and Workplace
Ensure that the machine and its safety equipment are kept in good working order.
Ensure that the work area is well lit, and protected from the elements, such as rain, snow, abrasive dust,
and extremes of temperature.
Ensure that the machine is installed with sucient clearance around it for the safe loading and unloading
of work pieces.
RESPONSIBILITIES OF THE OPERATOR AND MAINTENANCE PERSONNEL
Safety equipment
All machines are delivered with safety equipment that must not be removed or bypassed during operation.
The correct functioning of safety equipment on the machine must be checked:
• At the start of every shift.
• After maintenance and repair work
• When starting for the rst time, and after prolonged shutdowns
Emergency Stop Button (E-Stops)
Always be aware of the location of the Emergency Stop Button(s). Do not allow material or objects to
block your access to an Emergency Stop.
Damage
If any changes capable of impairing safety are observed in the machine or its operation, such as damage,
malfunctions, or irregularities, then appropriate steps must be taken immediately, the machine switched
o, locked-out, and the fault reported to the responsible person.
Safe operation
The machine may only be operated when in good working order and when all protective equipment is in
place and operational.
Keep a safe distance from all moving parts – especially the blade and vises.
Stock should not be loaded onto the saw if the blade is running.
Long and heavy stock should always be properly supported in front of and behind the saw.
Faults
The machine must be switched o and locked-out before starting to remedy any faults.
Safety hazard labels
Safety hazard labels and other instructional labels on the machine must be observed. They must be
clearly visible and legible at all times. If they become damaged they must be replaced.
0.4
Page 8
Clothing, jewellery, protective equipment
Personnel operating or working on the machine must not wear un-restrained long hair, loose-tting
clothes and dangling jewellery.
When operating or working on the machine, always wear suitable, ocially tested personal protective
equipment such as safety glasses and safety boots and any other equipment required by workplace
regulations.
Gloves
Experience has shown that careless use of gloves around machinery is a major factor in serious
hand injuries.
Gloves should not be worn when operating or adjusting the machine, except:
Wear protective gloves when handling bandsaw blades at blade changes.
Gloves may be worn when handling work pieces, only if the machine is in Manual Mode
and the bandsaw blade is not running.
If the machine is running in Auto Mode, and only if the cut parts are greater than 24
inches long, it may be possible to safely wear gloves for handling the cut parts, but the
wearer of the gloves must never put his hands near the blade for any reason. If the cut
parts are less than 24 inches long, it is required to arrange their automatic ow into a
parts bucket or other suitable arrangement to avoid the necessity to pick them o the
machine by hand.
Hearing protection
Ear protection must be worn whenever necessary.
The level and duration of noise emission requiring hearing protection depends upon the national
regulations in the country in which the machine is being used.
The actual level of noise emission by band sawing machines depends upon work piece size, shape and
material, blade type, blade speed and feed rate.
The only practical course of action is to measure the actual noise emission levels for the type of work that
is typically done. With reference to national standards, decide upon the necessary hearing protection
required.
In the absence of such measurements, it is advisable for anyone exposed to long periods of moderate to
loud noise to wear hearing protection. It is important to understand that hearing loss is gradual and easily
goes un-noticed until it is serious and irreversible.
Workplace
A clear working area without any obstructions is essential for safe operation of the machine. The
oor must be level and clean, without any build-up of chips, o-cuts, coolant, or hydraulic oil.
The workplace must be well lit, and protected from the elements, such as rain, snow, abrasive dust, and
extremes of temperature
Nothing may ever be placed on, or leaned against the machine, with the obvious exception of the work
piece on the table and conveyor of the machine.
Master Disconnect
Lock-out the machine before undertaking any maintenance or repair work on it. ‘Lock-out’ refers switching
o the master electrical disconnect switch, and locking it out so that it cannot be switched on again
without authorization.
0.5
Page 9
On Hyd-Mech machines the Master Disconnect Switch will be of one of four types:
• Rotary switch mounted in electrical control cabinet door and inter-locked with door.
• Rotary switch mounted on the side of the operator interface console.
• Lever switch mounted in separate box on the machine.
• Supply disconnect switch supplied by user at installation and usually wall-mounted within sight of
the machine, depending upon local regulations.
In almost all jurisdictions, it is required that owners of industrial equipment establish and post
lock-out procedures. Know and use the lock-out procedures of your company or organization.
Residual Risks
The machine is still not completely de-energized if an electrical cabinet door type switch is
locked-out.
The line side of the disconnect switch itself remains energized.
Variable speed blade drives store dangerous voltage in their capacitors, and this requires time to
dissipate. After locking out power, wait 3 minutes before beginning to work on machine electrical
circuits.
If compressed air is supplied to the machine to power a mist lubrication system or other devices,
it should be disconnected, and any stored air pressure released before working on the machine.
The weight of individual machine components represents stored potential energy that can be
released if they fall when disconnected. Secure these components with adequate hoisting gear
before disassembly.
SAFETY HAZARD LABELS
The safety hazard labels attached to your machine represent important safety information to help you avoid
personal injury or death.
All supervisors, operators, and maintenance personnel must locate and understand the safety information
associated with each hazard label prior to operating or servicing the machine.
The safety hazard labels shown below are located at various positions on the machine to indicate possible safety
hazards. The location and re-order part number of all the safety labels associated with this particular model of
bandsaw are indicated at the end of this section of the manual. It is important to replace any safety hazard label
that becomes damaged or illegible.
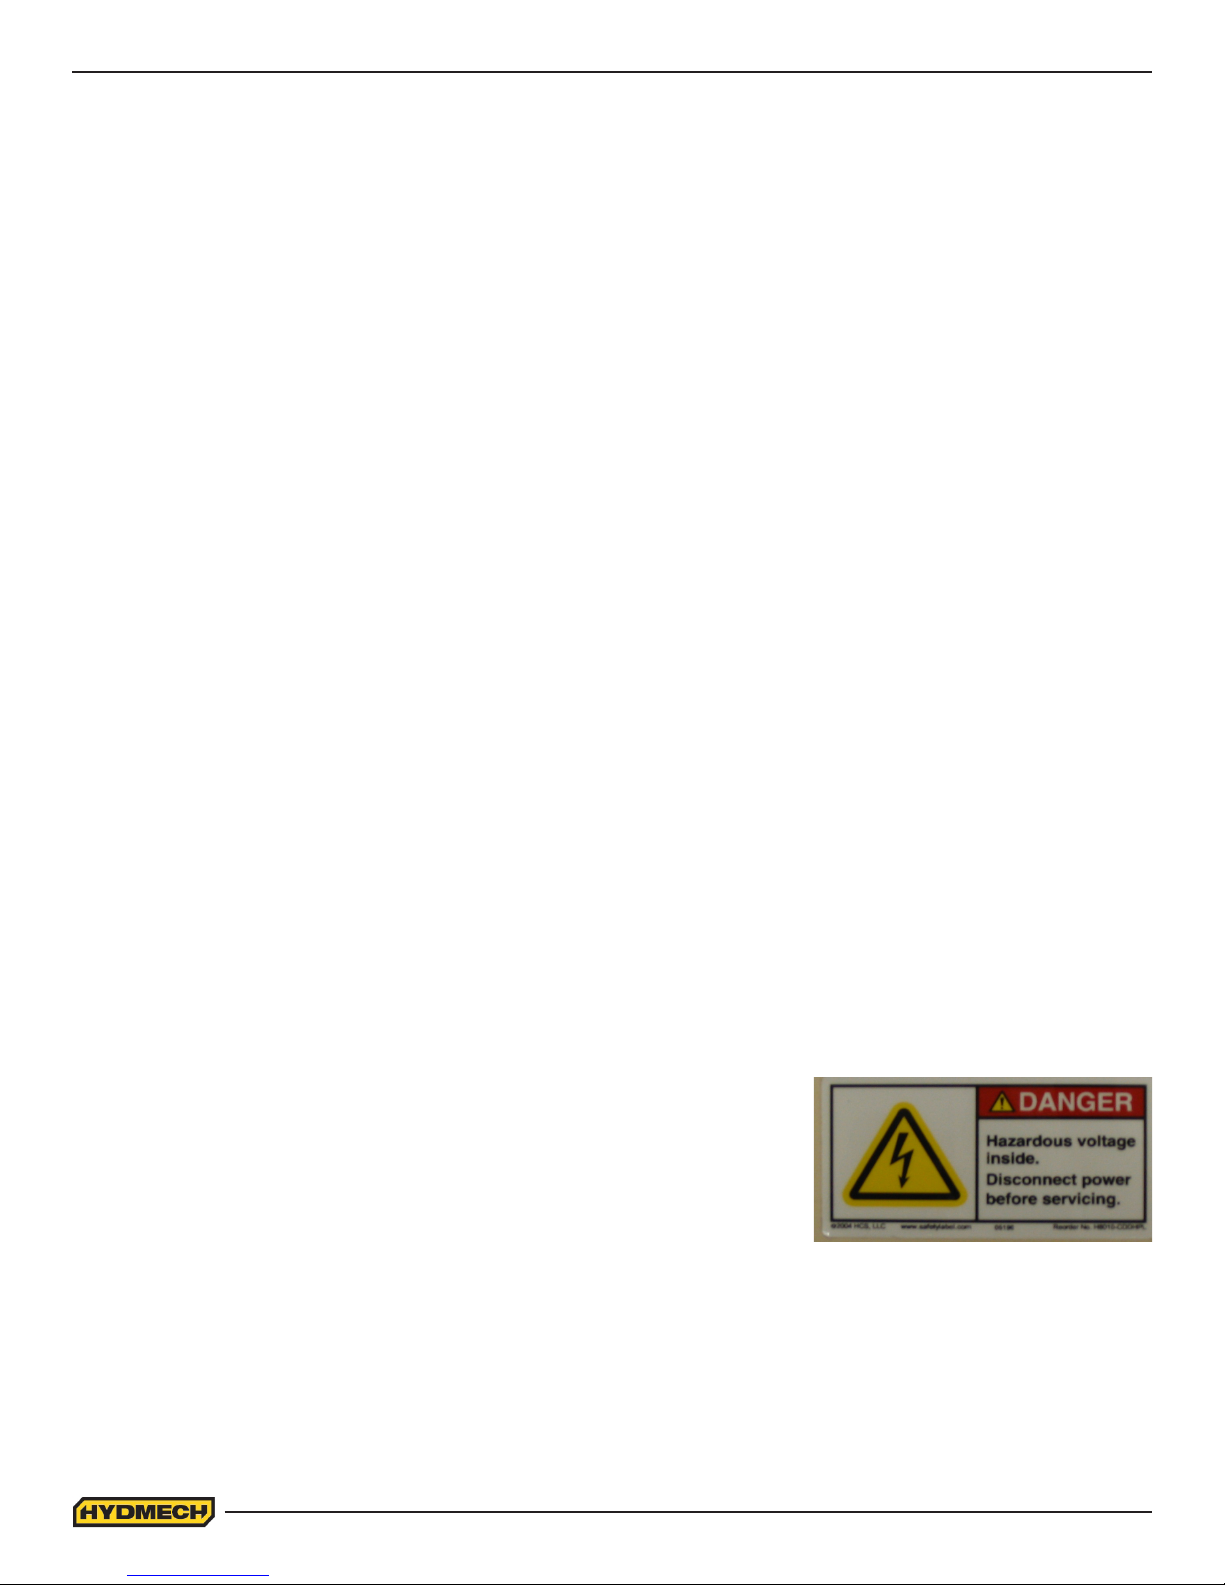
HAZARDOUS VOLTAGE INSIDE
Contact with high voltage may cause death or serious injury. Never perform
maintenance on, or near, electrical components until the machine’s electrical
power source has been disconnected. Lock-out power in accordance with
your company’s lock-out procedures before any such maintenance. The
“Stop” or “Emergency Stop” push button does not disconnect the machine’s
power supply. Hazardous voltage is still present in the machines electrical
circuits.
The machine’s Electrical Disconnect Switch does disconnect voltage from
the machine’s circuits; however hazardous voltage is still present inside the main electrical cabinet, on the infeed
(line) side of the main fuses. Therefore keep hands and tools away from the infeed side of the control panel main
fuses. If these fuses need to be replaced, use a fuse puller.
Allow three minutes after locking-out power before opening any electrical enclosures. Your machine may be
equipped with a variable frequency drive that stores high voltage within its capacitors. Three minutes will allow
sucient time for this voltage to safely discharge.
Never spray coolant directly at electrical components or cabinets.
0.6
Page 10
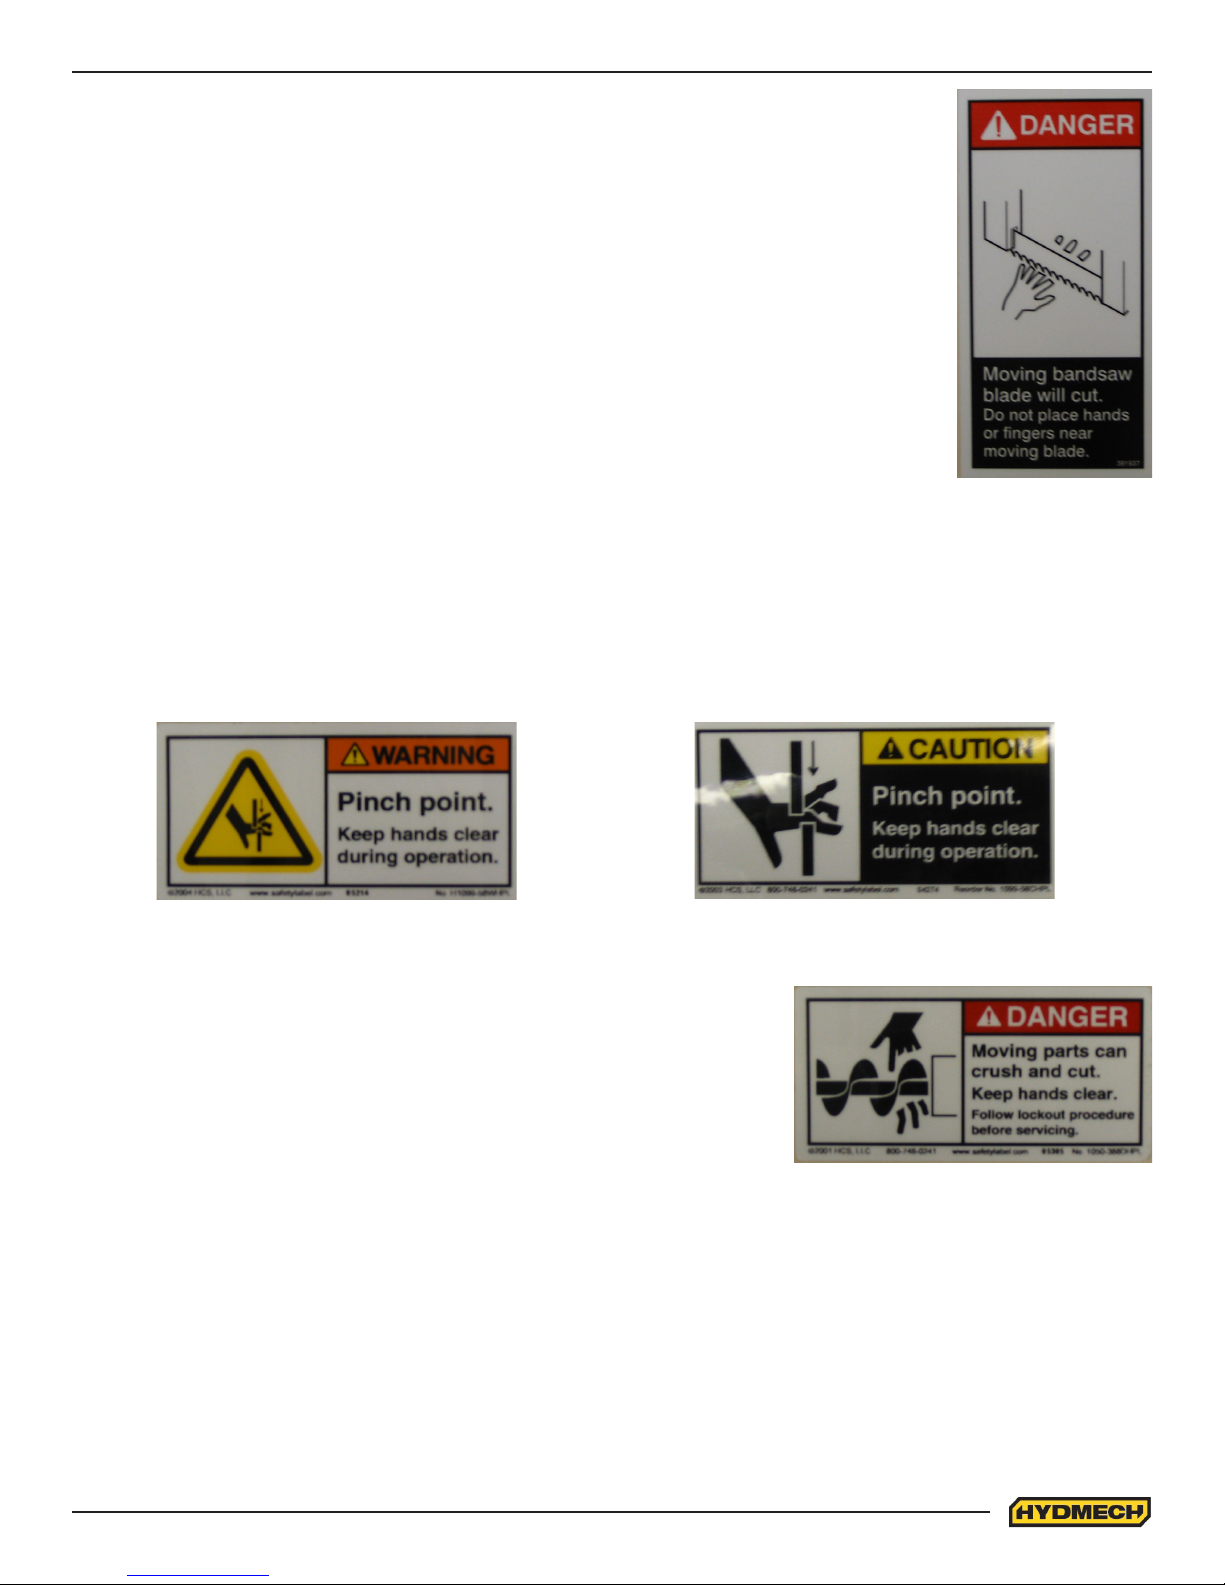
MOVING BANDSAW BLADE WILL CUT
Do NOT operate with guard removed.
Do NOT place hands or ngers near moving bandsaw blade.
For blade changing, always follow the proper Blade Changing Procedure, as given in
Section 3 of this manual.
PINCH POINT
Machine parts may move without warning, either because the machine is operating automatically, or because
another person initiates the motion. Keep hands clear of all labelled pinch points, whenever the machine is
running. Machine vises can exert great force and cause severe injury. Keep hands clear of vises and work piece
when vises are opened or closed. Be aware that vise closing or opening may result in potentially dangerous work
piece movement. Be aware also that the opening motion of a vise may create potential pinch points.
MOVING PARTS CAN CRUSH AND CUT
Keep hands clear of chip auger. Lock-out power in accordance with your
company’s lock-out procedures before attempting to clear a jam in the
chip auger.
Be aware that the chip auger may start unexpectedly, either because the
machine is operating automatically, or because another person initiates
the motion.
If the chip auger is stalled because of a jam, it may start without warning
when the jam is cleared, unless the machine power is locked out.
0.7
Page 11
SECTION 1 - INSTALLATION
Upon delivery of your new H-40 saw, it is imperative that a thorough inspection be undertaken to check for any
damage that could have been sustained during shipping. Special attention should be paid to the electrical and
hydraulic systems to check for damaged cords, hoses and uid leaks. In the event of damage caused during
shipping, contact your carrier to le a damage claim.
SAFETY PRECAUTIONS
The H-40 has been designed to give years of reliable service. It is essential that operators be alerted to the
safe operation of this saw, and the practices to avoid that could lead to injury. The following safety rules are at
the minimum necessary for the safe installation, operation, and maintenance of the saw. Take every precaution
for the protection of operators and maintenance personnel. At the beginning and through out this manual there
are precautionary indicators, these will inform you of areas which require special attention.
• POWER HOOK-UPS AND REPAIRS SHOULD BE ATTEMPTED ONLY BY QUALIFIED TRADESMEN.
• THE SAW SHOULD BE LOCATED IN AN AREA WITH SUFFICIENT ROOM TO SAFELY LOAD STOCK
INTO THE SAW. SECURE THE SAW TO THE FLOOR.
• THE AREA AROUND THE SAW SHOULD BE MAINTAINED IN A CLEAN AND TIDY CONDITION TO
AVOID OBSTACLES OPERATORS COULD TRIP OVER.
• THE H-40 SAW SHOULD ONLY BE OPERATED ACCORDING TO THE SPECIFICATIONS OF THE
SAW AVOID UNSAFE USAGE PRACTICES.
• IF AT ANY TIME THE SAW DOES NOT APPEAR TO BE OPERATING PROPERLY IT SHOULD BE
STOPPED IMMEDIATELY AND REPAIRED.
OPERATOR:
• THE SAW SHOULD NEVER BE OPERATED UNLESS ALL GUARDS AND DOORS ARE IN PLACE AND
CLOSED.
• KEEP A SAFE DISTANCE FROM ALL MOVING PARTS – ESPECIALLY THE BLADE AND VISES.
• LOOSE CLOTHING AND GLOVES SHOULD NEVER BE WORN WHILE OPERATING THE SAW,
COVER LONG HAIR.
• STOCK SHOULD NOT BE LOADED ONTO THE SAW IF THE BLADE IS RUNNING.
• LONG AND HEAVY STOCK SHOULD ALWAYS BE PROPERLY SUPPORTED IN FRONT OF AND
BEHIND THE SAW.
• NEVER ATTEMPT TO DISLODGE OR MOVE STOCK WHILE THE BLADE IS MOVING. TAKE THE
TIME TO STOP THE SAW BLADE, REMOVE OBSTRUCTIONS, AND RESTART BLADE.
• MUST WEAR EYE PROTECTION.
• MAINTAIN PROPER ADJUSTMENT OF BLADE TENSION, BLADE GUIDES, AND BEARINGS.
• HOLD WORKPIECE FIRMLY AGAINST TABLE.
• DO NOT REMOVE JAMMED CUTOFF PIECES UNTIL BLADE HAS STOPPED.
NO MODIFICATIONS TO THE MACHINE ARE PERMITTED WITHOUT PRIOR APPROVAL FRO HYD-MECH. ANY
APPROVED MODIFICATIONS SHOULD ONLY BE UNDERTAKEN BY TRAINED PERSONNEL.
1.1
Page 12
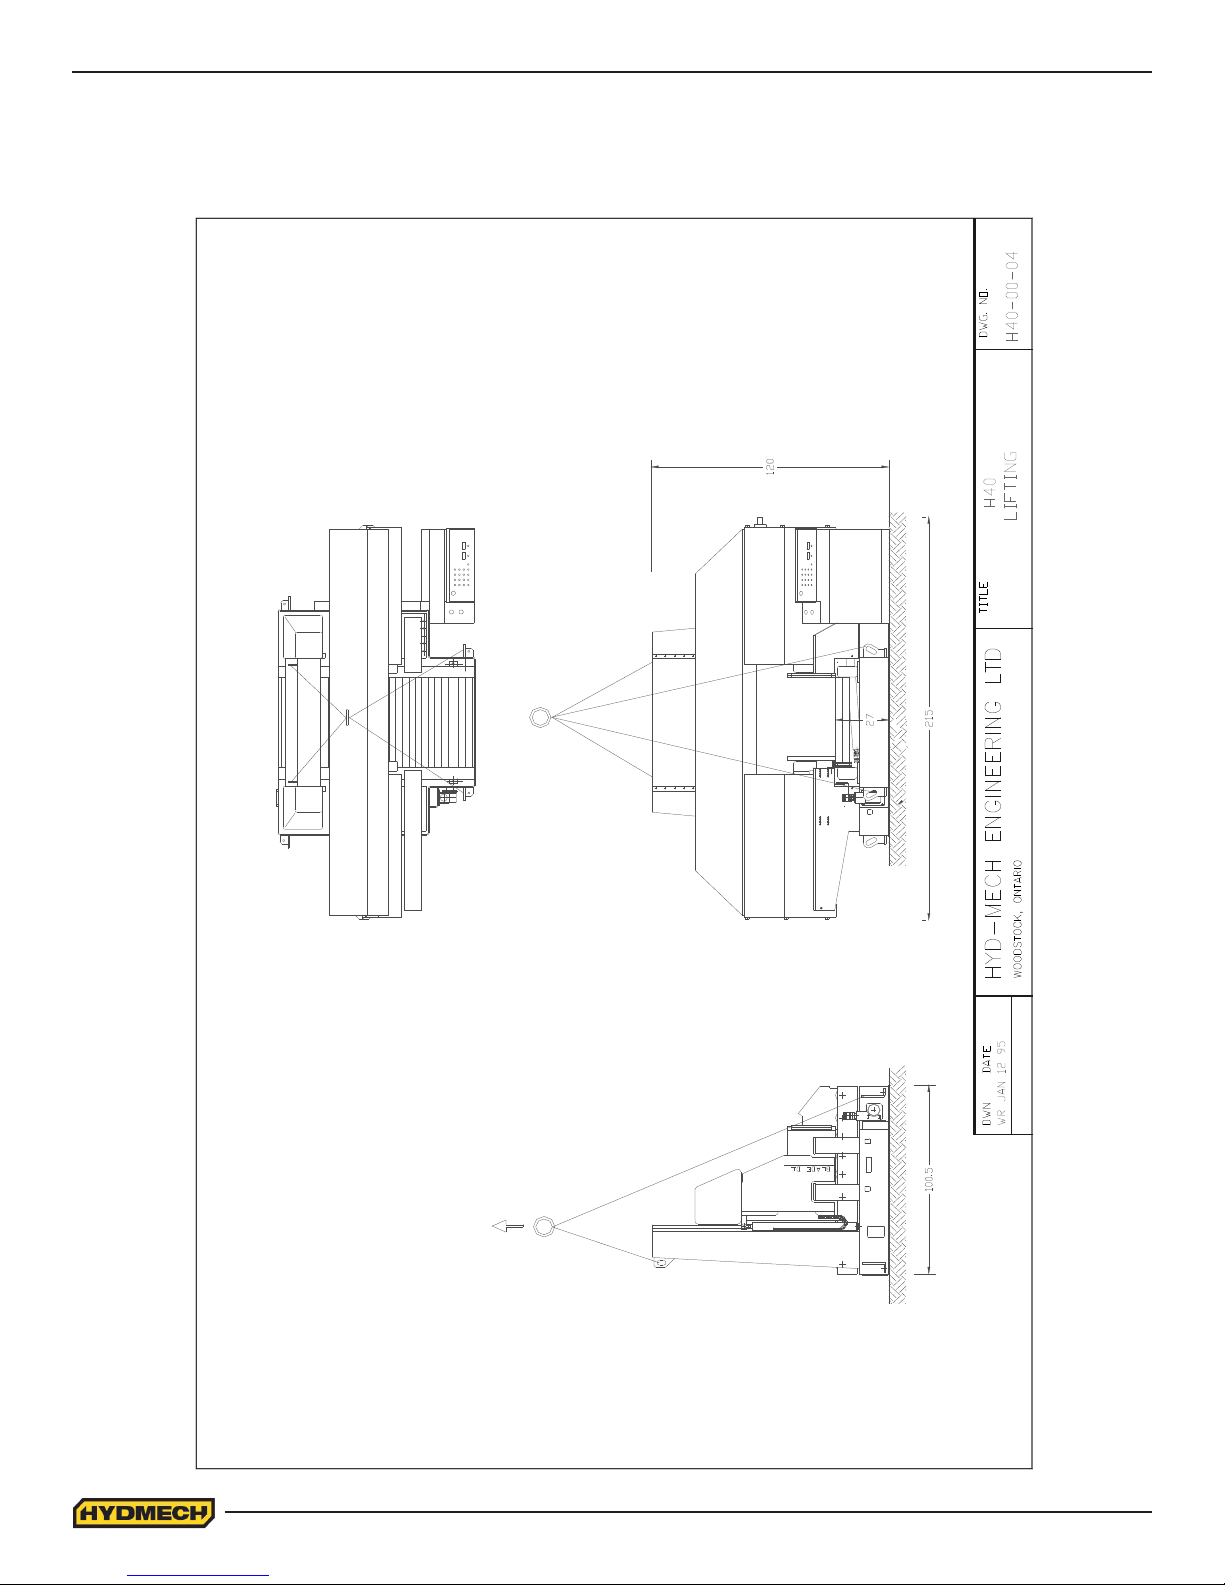
LIFTING THE H-40
The machine weight for a H40-40 is 39,000lbs (17690Kg) or 42,000lbs (19051Kg) with the optional outboard vise.
The machine weight for a H40-60 is 42,000lbs (19051Kg) or 45,000lbs (20412Kg) with the optional outboard vise.
The machine weight for a H40-80 is 46,000lbs (20865Kg) or 50,000lbs (22680Kg) with the optional outboard vise.
1.2
Page 13
THE DATA/DESIGN CONTAINED HEREIN IS PROPRIETARY
AND CONFIDENTIAL.REPRODUCTION,PUBLICATION OR
DISTRIBUTION OF ANY PART REQUIRES WRITTEN CONSENT
OF HYD-MECH GROUP.THIS DATA IS THE PROPERTY OF
HYD MECH GROUP AND ITS POSSESION CONFERS NO
LICENSE TO USE OR RIGHT OR LICENSE TO DISCLOSE IT
TO OTHERS FOR ANY PURPOSE WHATSOEVER.
ALL RIGHTS RESERVED.
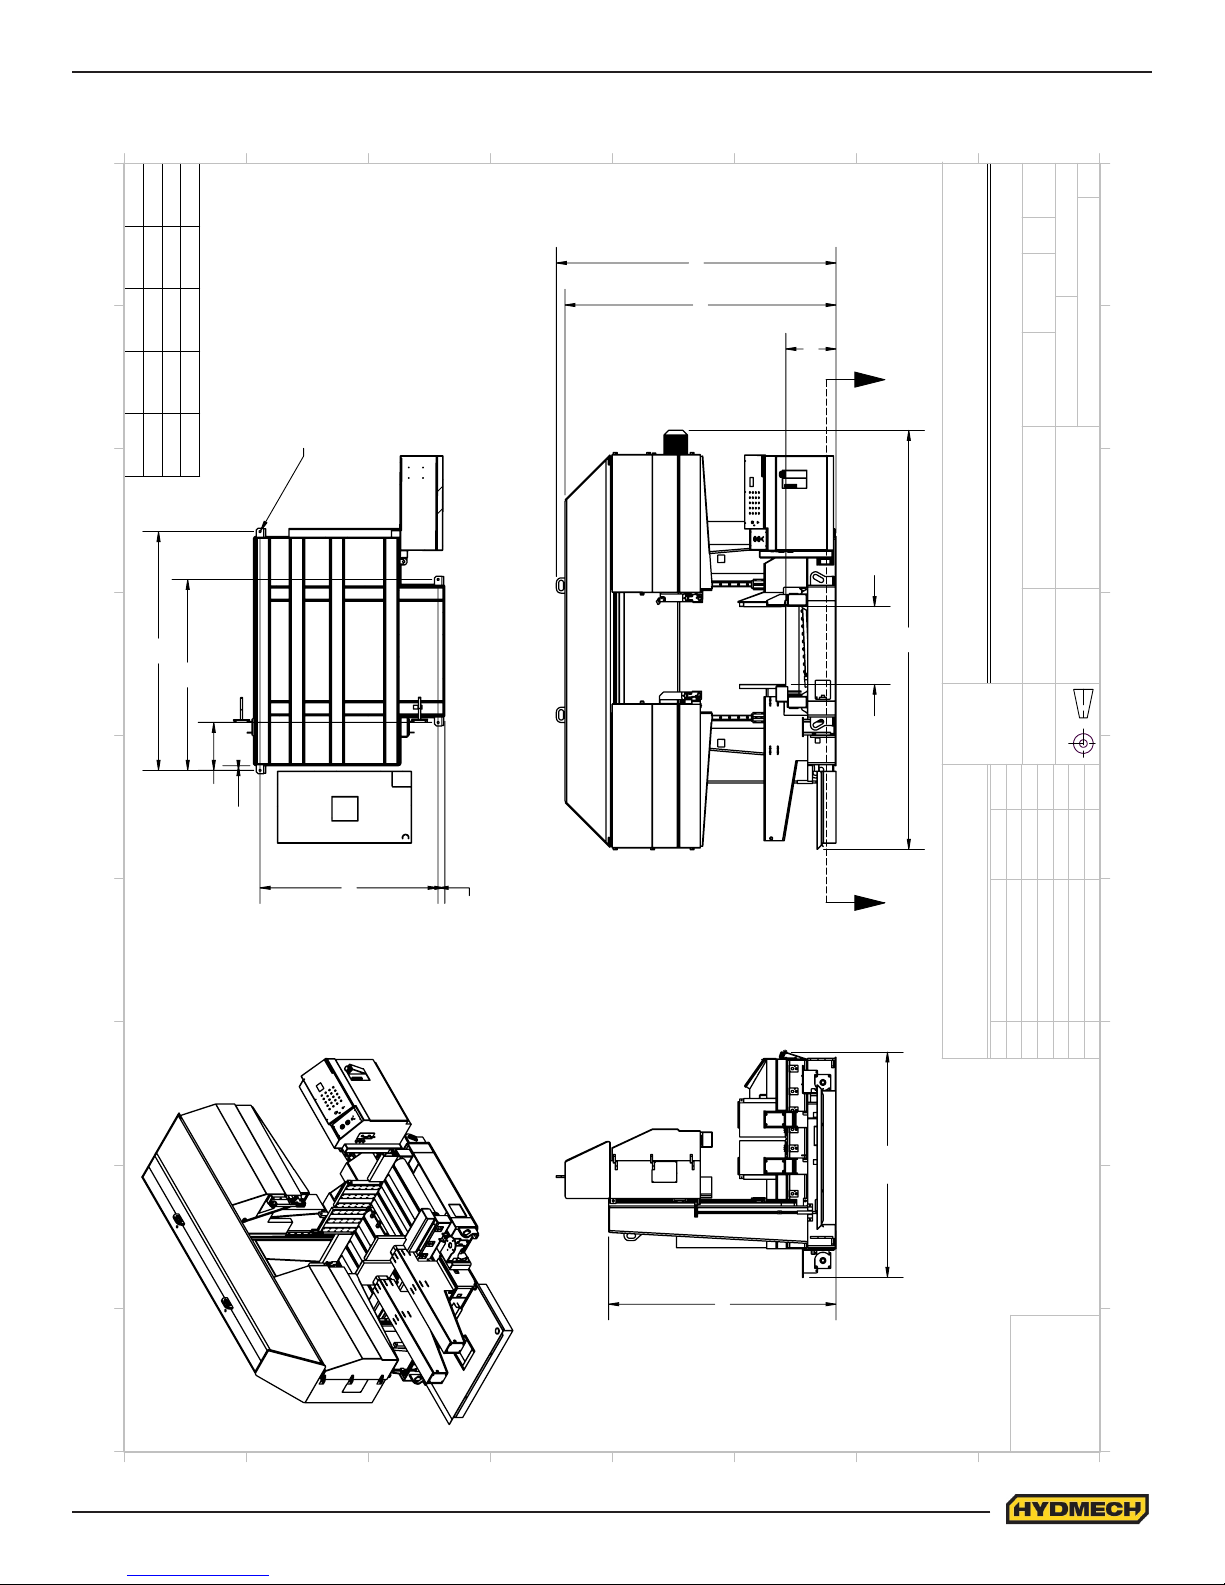
MACHINE LAYOUT
8
J
126"
146"
100.75"
120.75"
I
221"
241"
A B C D
41"
61"
H
H4040
H4060
166"
140.75"
261"
81"
H4080
7
6
1-8 UNC (x4)
5
4
3
148
143
27
2
1
SHEET
SCALE
CHKED BY:
1
OF
1
1:66
DATE:
COATING:
0
REV
-
No Coating
J
I
H40-0-00
AA
EngCoop
Jan 21, 2016
DRWN BY:
PART WEIGHT:
DRAWING NUMBER:
DATE:
WOODSTOCK. ONTARIO. CANADA N4S 0A9
H
HYDMECH GROUP LIMITED
MAT'L:
COMPONENT GROUP:
G
B
D
C
SECTION A-A
A
00 - Top Level
MODEL:
H4040
TITLE
H4040, H4060, H4080 MACHINE LAYOUT
G
MATERIAL CODE:
FOUNDATION PLAN
F
UNLESS
HYDMECH
STANDARD
TOLERANCES
SPECIFIED
OTHERWISE
DIMENSIONS
-
-
BY
ARE IN INCHES
THIRD ANGLE PROJECTION
F
25.25
2.5
E
DATE
-
-
E
94
3.5
REVISIONS
-
-
ECN NUMBER
D
C
B
120
119
REV
-
-
D
C
B
A
8
7
6
5
4
3
2
1
A
0
1.3
Page 14
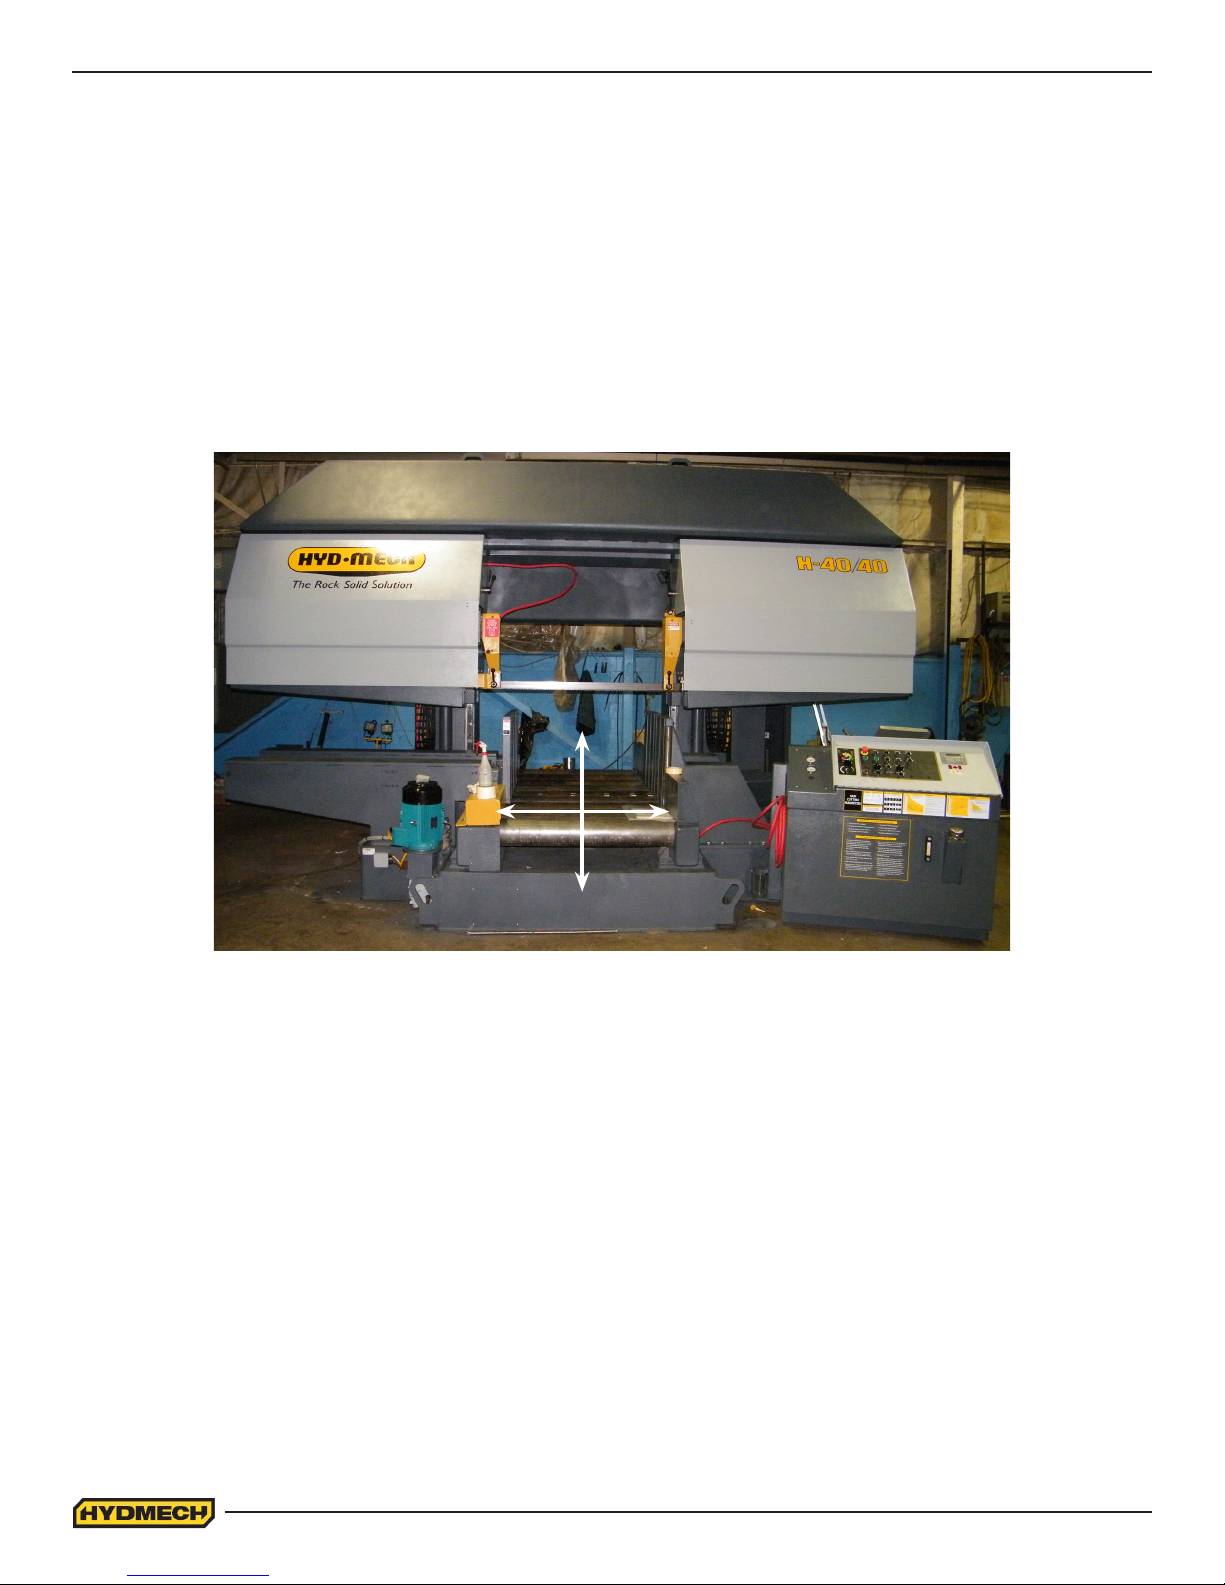
FOUNDATION, LEVELING AND ANCHORING
Machine location should be carefully selected. A at concrete oor area should be chosen. It should have enough free
space surrounding the machine to enable free access for safe operation and maintenance.
The machine should be leveled in both directions, i.e. along and across its infeed conveyor especially when machine is to
be inserted into a larger conveyor system. The photo below shows the conveyor from the infeed side.
Four leveling screws are provided, one in each corner of the machine base. Steel plates are to be placed under each
screw to prevent their sinking into the concrete oor.
NOTES: In some cases leveling the saw infeed and auxiliary conveyors with a slight slope towards the blade are recommended. This will prevent coolant from running down the raw stock. (This is especially true when cutting tubing or bun-
dles).
H-40 INSTALLATION PROCEDURE
1) Machine location should be carefully selected. A at concrete oor area should be chosen and have enough free
space surrounding the machine to enable free access for safe operation and maintenance.
2) Cut strapping and remove conveyor drive & chip bucket from saw rollers.
3) Remove coolant tank & position at the left side of the saw (facing from front).
4) Remove leveling pads from inside coolant tank & place under saw base leveling bolts.
5) Check machine level from side to side & back to front. A slight incline (1/8”-1/4” rear of saw higher) will assist
coolant ow back into return tray. Ideally if the machine is sitting at on the oor & the level is good do not
touch leveling bolts. If leveling bolt adjustment is necessary use shims supplied and place under 6 corners of
base frame. Remove leveling bolts and re-check level. If level is unchanged anchor machine to the oor using
adjusting bolt holes.
6) Install infeed conveyor drive with bolts supplied. Install the conveyor drive chain.
1.4
Page 15
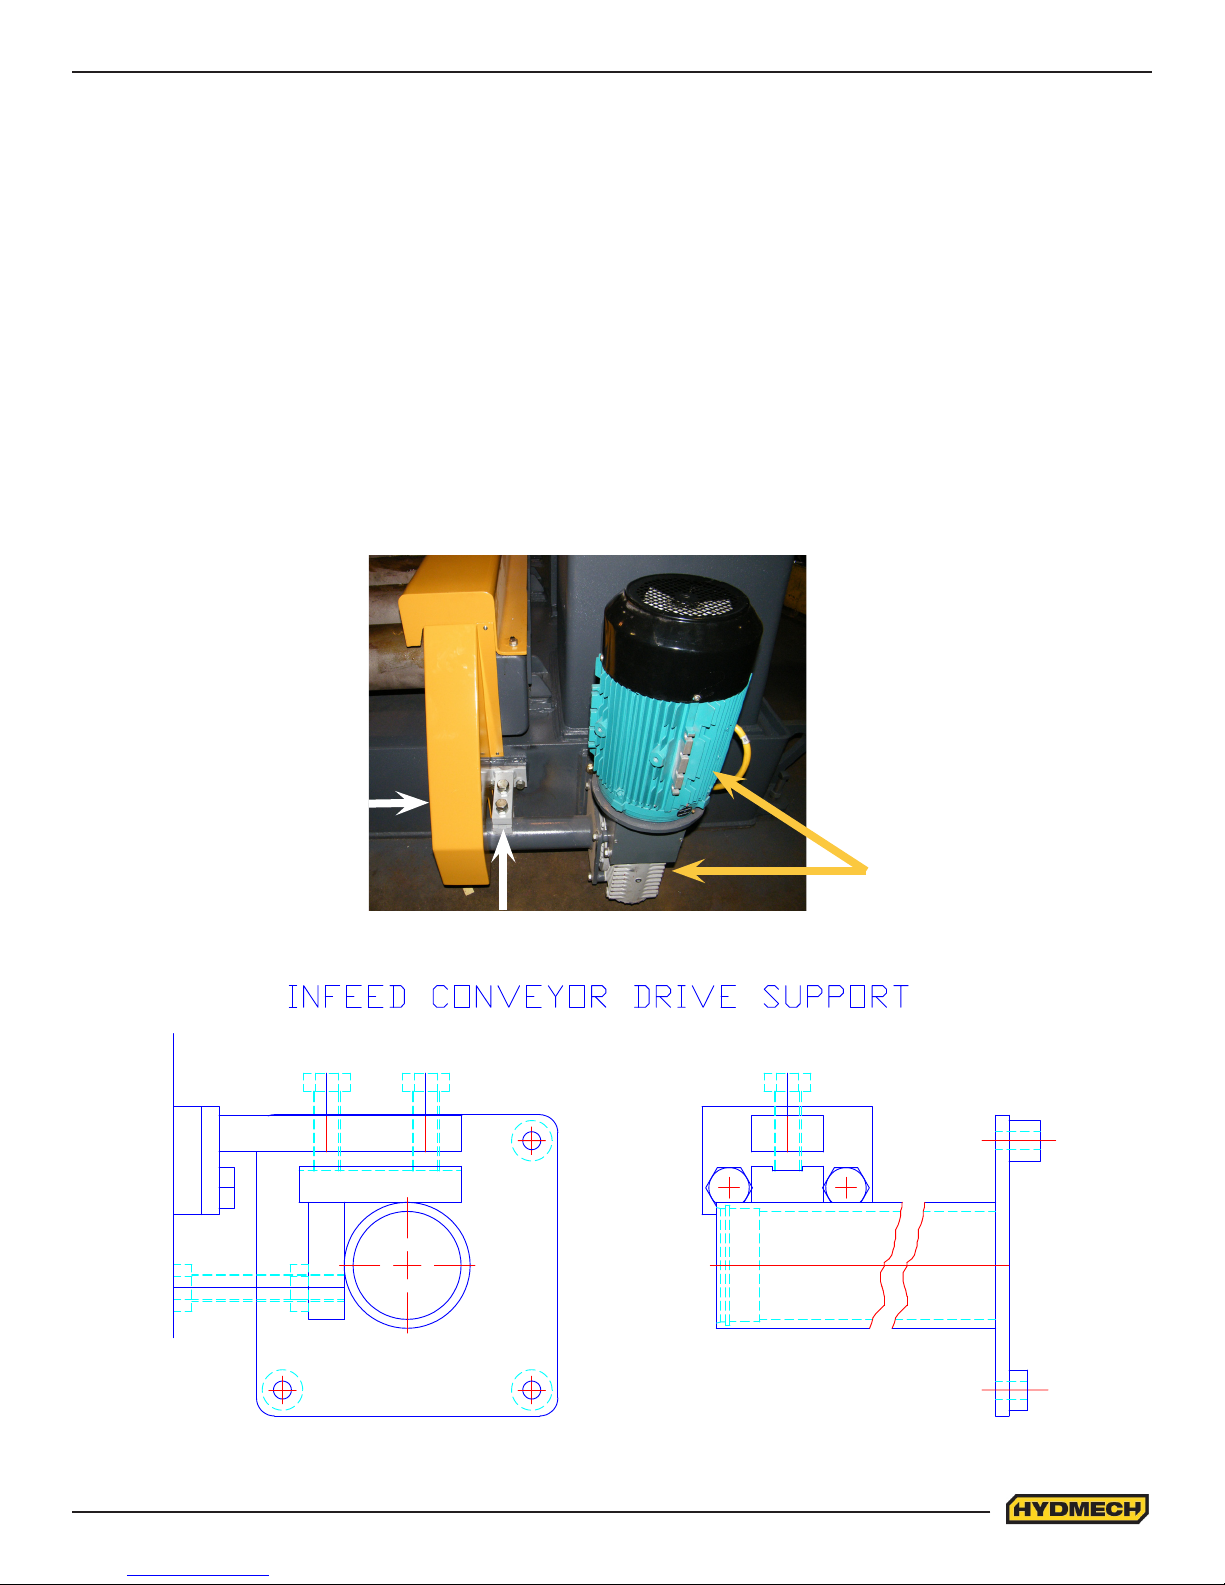
For machine shipping purposes the following items have been removed from the saw.
• Infeed conveyor gearbox and motor
• Bearing housing support
• Chain guard
Once the machine has been installed, levelled and anchored the above three items are to be installed as follows:
1. Install the gearbox and motor (1) using the four bolts and use the gearbox as a tensioner by moving it up and
down before completely tightening the four bolts.
2. Install the chain guard over the sprockets.
3. Install the bearing housing support (2).
4. Install the chain guard (3).
3
1
2
1.5
Page 16
HYDRAULIC OIL AND CUTTING FLUID
The H-40 bandsaw is supplied with Texaco 46 hydraulic oil. If it in necessary to change the oil to dierent brand see the
HYDRAULIC SECTION for equivalent grade oil.
No cutting uid is supplied with machine. There are two types of coolant available:
-Oil based; dilute 1:10 ratio. (one part concentrated coolant to 10 parts water)
-Synthetic; dilute as recommended by the manufacturer.
WIRING CONNECTIONS
After the machine is leveled and anchored the necessary power hook-up needs to be performed. In order to provide
a safe operation as well as to prevent potential damage to the machine, only qualied personnel should make the
connections.
BEFORE START-UP THE FOLLOWING TWO POINTS SHOULD BE CHECKED:
-Signs of damage that may have occurred during shipping to the electrical cables and the hydraulic hoses.
-The hydraulic oil level is between the upper and lower lines on the level gauge on the front of the control panel base.
As supplied, the machine is set to run on three phase voltage as indicated on the serial plate and voltage label. Power
connection to the machine is made to machine disconnect and ground connections inside the electrical panel as shown
below.
During the initial hook-up it is very important to check that the phase order is correct. This is indicated by the hydraulic
pressure gauge registering a pressure rise and the blade running in a counter clockwise direction. If the hydraulics do not
register an immediate pressure rise, shut the hydraulics o and change the phase order.
ATTENTION:
1) Running the hydraulics “backwards” can damage the hydraulic pump.
2) After checking the hydraulic pressure and BEFORE INSTALLING the drive chain between
the infeed conveyors, check that the conveyors are running in the correct direction. If they are
not, change any two phases at the MOTOR JUNCTION BOX for each motor as required.
Power connections should be made by qualied personnel only
1.6
Page 17
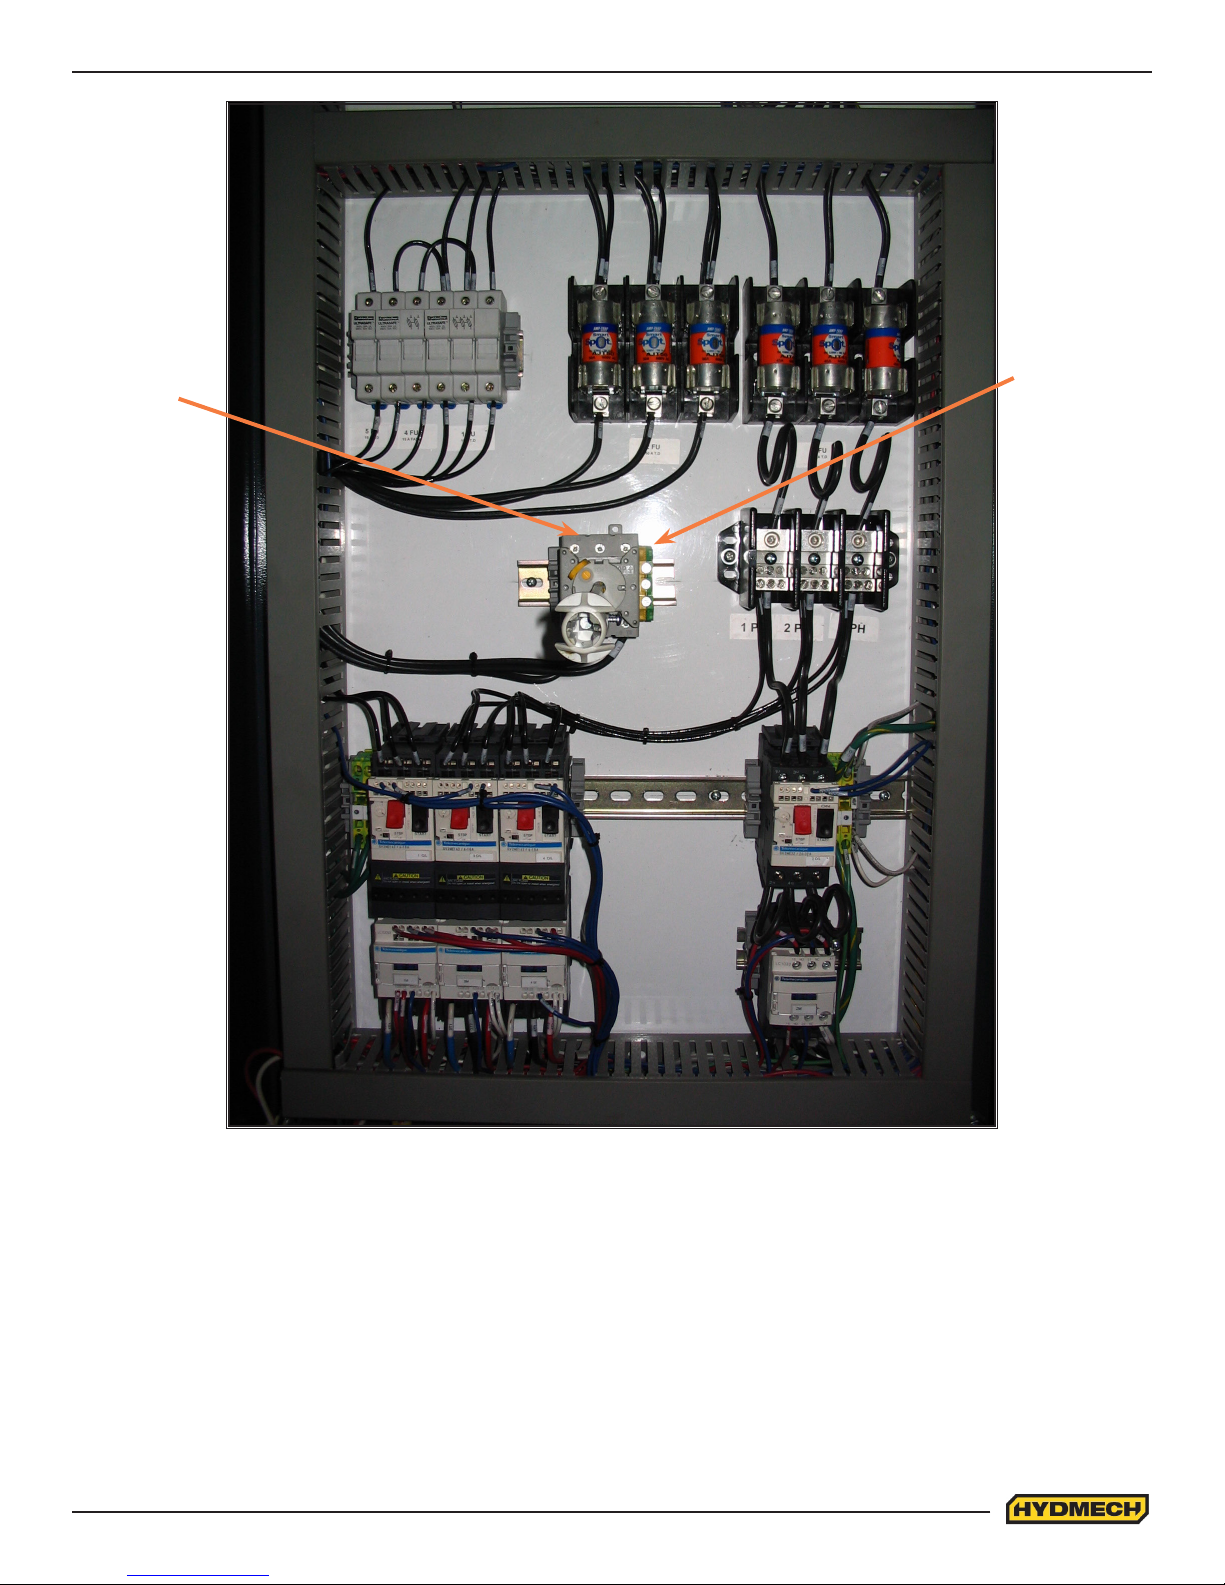
L1 L2 L3
Ground
connection
Electrical panel located
behind the head on the
drive side
1.7
Page 18
SECTION 2 - OPERATING INSTRUCTIONS
This section has been prepared to give the operator the ability to set up the saw for most cutting situations. Before cutting
any material, the operator should be familiar with all operations and controls as well as the basic cutting theory described
below. The saw is equipped with variable blade speed and hydraulic feed control, as well as an extensive door chart to
guide the operator to the correct setting of these controls.
BLADE BASICS
Technology is rapidly changing all aspects of production machining. Metal cuto is no exception. The advances made
in the bandsaw blade industry have denitely brought down the cost per cut, despite the three fold higher price of high
technology blades. Variable pitch, bi-metal blades (like the 4/6 or 3/4 bi-metal blade supplied with the machine) last much
longer, cut faster, and more accurately than conventional carbon steel blades. In order to take advantage of the superiority
of bi-metal blades, it is critical to properly “break-in” a new blade. This is accomplished by taking two or three cuts through
solid four or ve inch diameter mild steel at an extremely slow feed rate. (It is also advisable to utilize a slow blade speed)
These two or three slow cuts suciently lap (polish) the teeth on the new blade so that it does not snag the material being
cut. Proper break-in will alleviate blade vibration; improve surface nish, accuracy, and blade life.
After “break-in”, the following six points must be closely monitored to ensure long blade life:
1. Proper blade tension should be maintained. (See Section 3, Maintenance and Troubleshooting)
2. Generous coolant application is essential with most materials. A high quality and well mixed coolant will extend
blade life, and also increase cutting rate and quality. On those materials where coolant is undesirable for cutting,
a slight coolant ow or periodic oiling of the blade is necessary to prevent the blade from being scored by the
carbide guides.
3. The stock being cut must be securely clamped in the vises.
4. The proper feed force should be chosen. (see Saw Cutting Parameters: Step 2)
5. The proper blade speed must be selected. (see Saw Cutting parameters: Step 4)
6. The proper feed rate must be applied. (see Saw Cutting Parameters: Step 5)
VARIABLE SPEED CONTROL
Blade speed can be adjusted innitely between 75 and 270 SFM (Surface Feet/Minute) (23 to 82 m/min) Adjustment
should be made only when the blade is running. Clockwise rotation of the knob increases blade speed while counter
clockwise rotation decreases blade speed.
THE CONTROL PANEL
START-UP
The control console has been designed to simplify the operation of the saw, to give the operator the ability to stop any
function at any time, and to be able to control all the functions remotely. We cannot overstress the importance of
familiarizing yourself with the controls prior to star ting the machine.
NOTE:
1. ALL SWITCHES MUST BE IN THE CENTER NEUTRAL POSITION TO START THE MACHINE!
2. WHEN STARTING THE MACHINE FOR THE FIRST TIME MAKE SURE THAT BLADE IS MOVING IN A
COUNTERCLOCKWISE DIRECTION, AND THAT THE HYDRAULIC PRESSURE IS:
-1200 PSI FOR H-40/40 AND H-40/60
-1300 PSI FOR H-40/80
MANUAL OPERATION
Manual Operations can be performed by using the control buttons on the HMI. All functions are self-explanatory. Specic
control button functions are described on the following pages.
2.1
Page 19
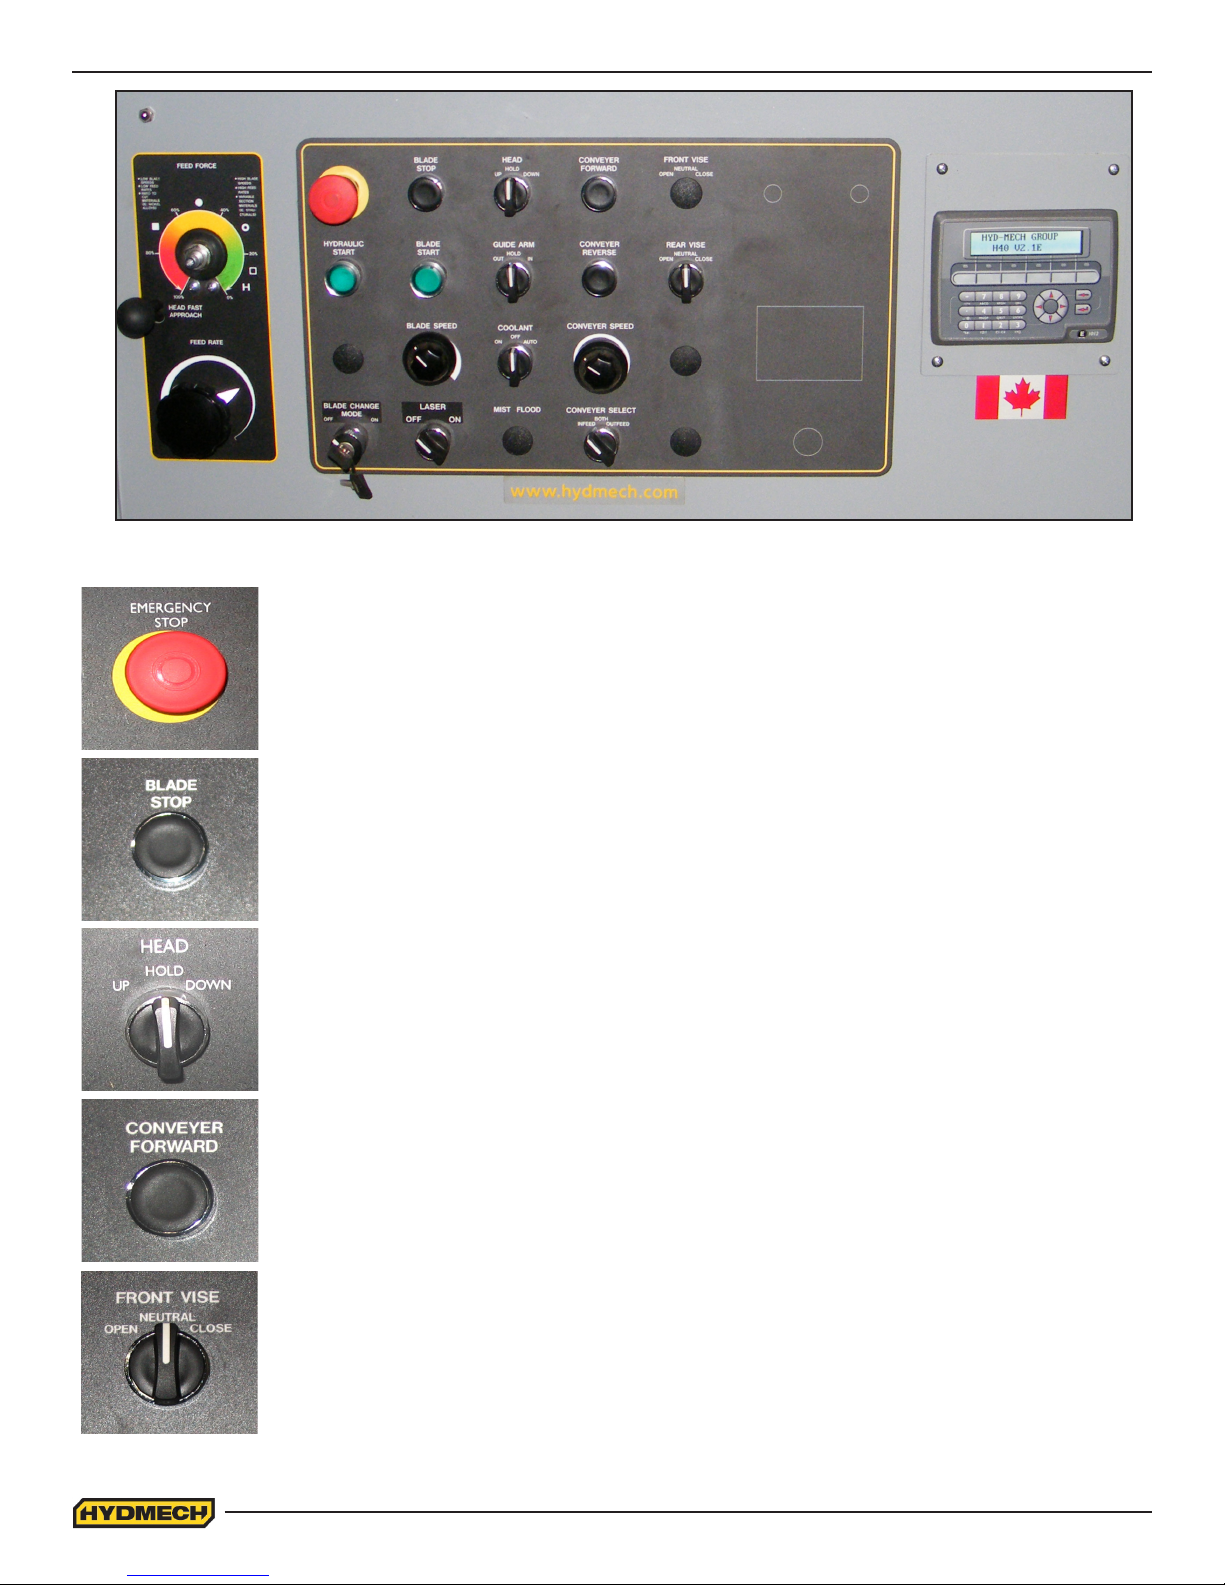
EMERGENCY STOP
Stops blade and hydraulic motors. Head motion will stop and vise clamping pressure will begin to
fall o. Long pieces of work should always be supported so they will not become loose over time
and fall while the machine is shut down. This is a latched button and must be pulled out to start
the machine.
BLADE STOP
When depressed the blade will stop. Blade motor will stop automatically when head reaches
head down limit switch.
HEAD CONTROL
This switch has three positions: UP, HOLD, and DOWN. UP causes head to rise until it
mechanically cannot raise any higher or the switch is moved to HOLD. In HOLD head movement
stops. In the DOWN position the head will descend until it reaches the lower limit switch. The
speed or rate of descent is controlled by the FEED RATE VALVE.
CONVEYOR FORWARD
When depressed, the selected conveyor’s rollers rotate in a direction which would move material
forward from behind the saw head toward the front of the machine. Releasing the push button
deactivates conveyor motor(s) and movement will stop.
FRONT VISE
This switch has three positions, OPEN, NEUTRAL and CLOSE. With the switch held in the
OPEN position the vise will open all the way or until the switch is released. With the switch in the
NEUTRAL position, the vise will stay where it is and will not move freely although it will not resist
a large force indenitely without creeping. In CLOSE, the vise will close all the way, or until it
encounters enough resistance to stop it.
2.2
Page 20
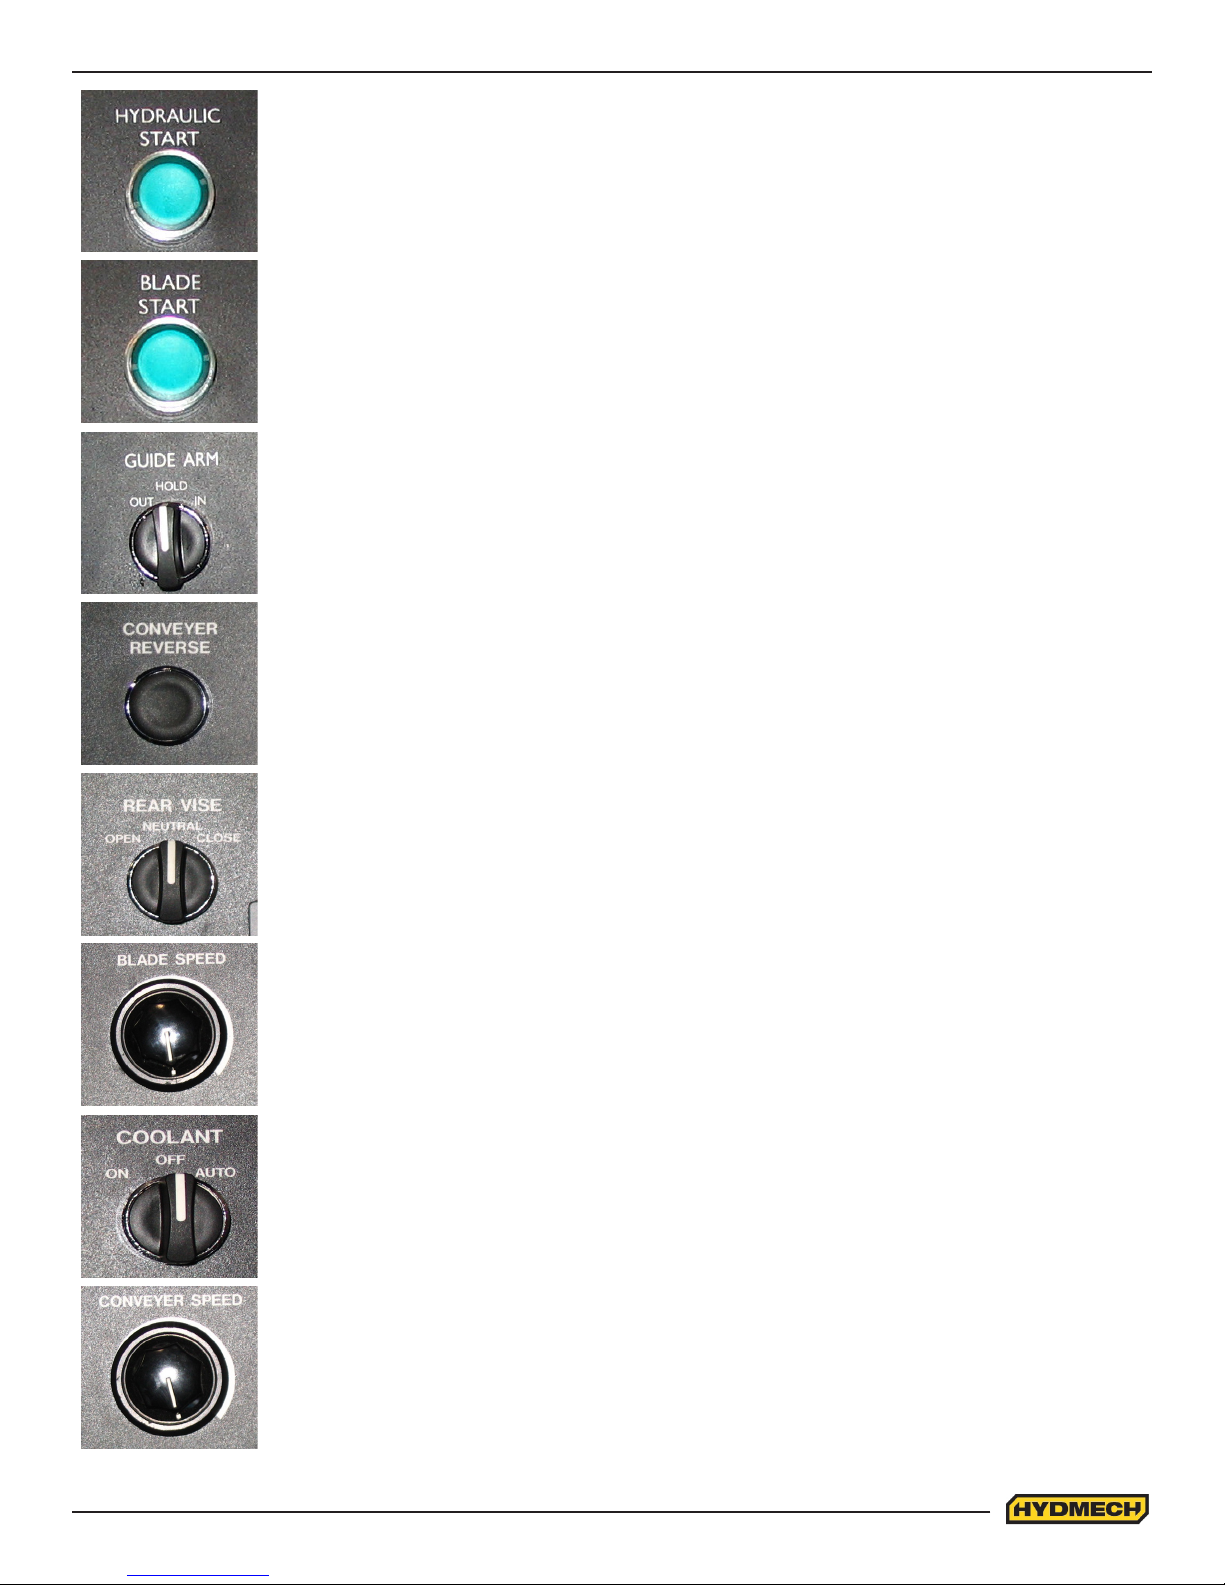
HYDRAULIC START
To start the hydraulic system, the switches for the head and vises must be in the “NEUTRAL”
position. The “HYDRAULIC START” button must be depressed and held in momentarily until the
PLC display becomes active.
BLADE START
Starts the blade when depressed. Only active with hydraulics running and saw head up, o of
lower limit switch.
GUIDE ARM
Three position, spring centered switch. When held to the IN position, the moveable guide arm will
move in toward the xed guide arm. OUT retracts the moveable arm away from the xed guide
arm. When released, the switch returns to the center position allowing no guide arm movement.
ENSURE CLEARANCE BETWEEN GUIDE ARM AND VISES AT ALL TIMES.
CONVEYOR REVERSE
When depressed, the selected conveyor’s rollers rotate in a direction which would move material
toward the back of the machine. Releasing the push button deactivates conveyor’s motors and
movement will stop.
REAR VISE
This switch has three positions, OPEN, NEUTRAL and CLOSE. With the switch held in the
OPEN position the vise will open all the way or until the switch is released. With the switch in the
NEUTRAL position, the vise will stay where it is and will not move freely although it will not resist
a large force indenitely without creeping. In CLOSE, the vise will close all the way, or until it
encounters enough resistance to stop it.
BLADE SPEED
Allows for increase or decrease of blade speed while blade motor is running.
COOLANT
This switch has three positions, AUTO, OFF, and ON. In the ON position, the coolant system
will operate when there is power to the machine; this allows using the wash gun to clean the
machine. In the OFF position, the coolant system is inactive. In the AUTO position the coolant
system will only run when the blade is on. The coolant system can also be run only when both
the blade is on and the head is descending by selecting this option in the PLC parameters.
CONVEYOR SPEED
Allows for increase or decrease in speed of selected conveyor(s) when FORWARD or
REVERSE push buttons are depressed.
2.3
Page 21
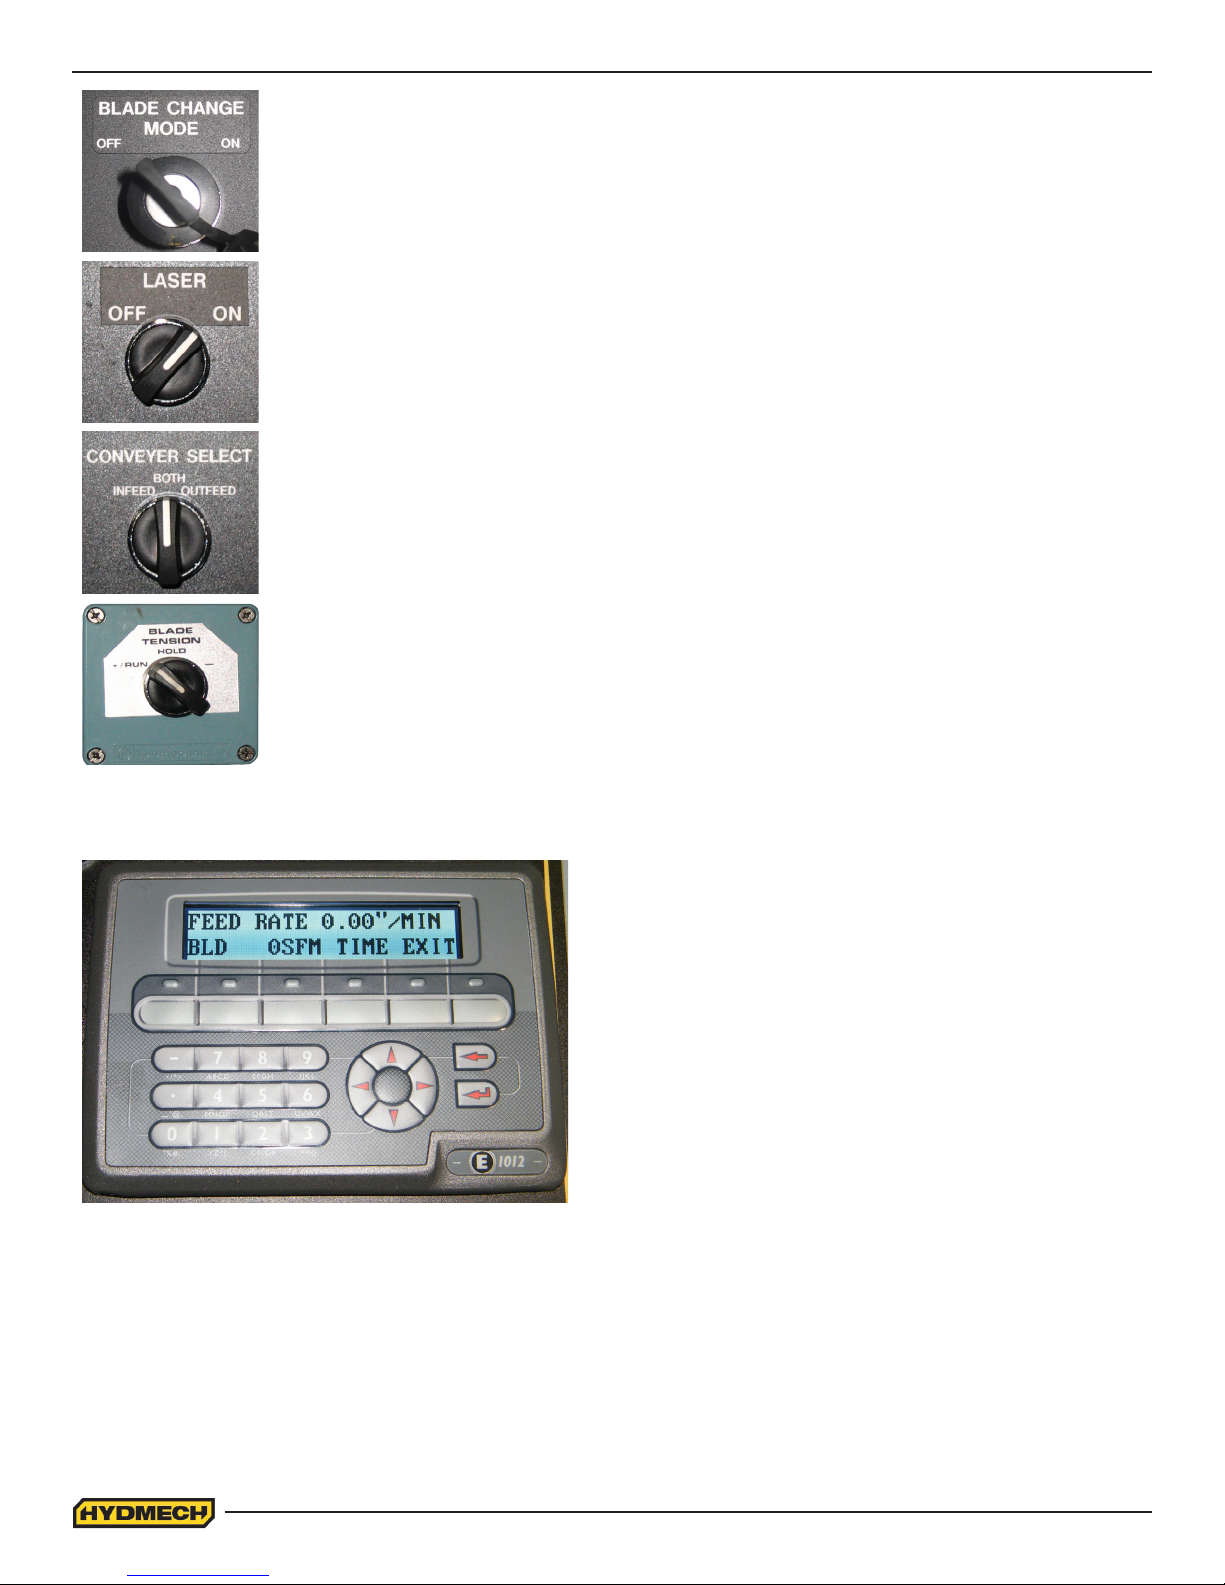
SAFETY LOCK
This lock is provided for the safety of the operator during the blade changing procedure. When
the lock is in the “ON” position, the door interlocks are disabled and the only functions that are
active are the HEAD and BLADE TENSION controls. All other controls are inactive. After the
blade has been changed the lock must be switched to “OFF” in order to operate the machine.
LASER
This option switch has two positions, OFF & ON.
CONVEYOR SELECT
Three maintained positions: INFEED, BOTH, and OUTFEED. Selects the conveyor(s) to move
when the CONVEYOR FORWARD or REVERSE PUSH BUTTONS are used.
BLADE TENSION
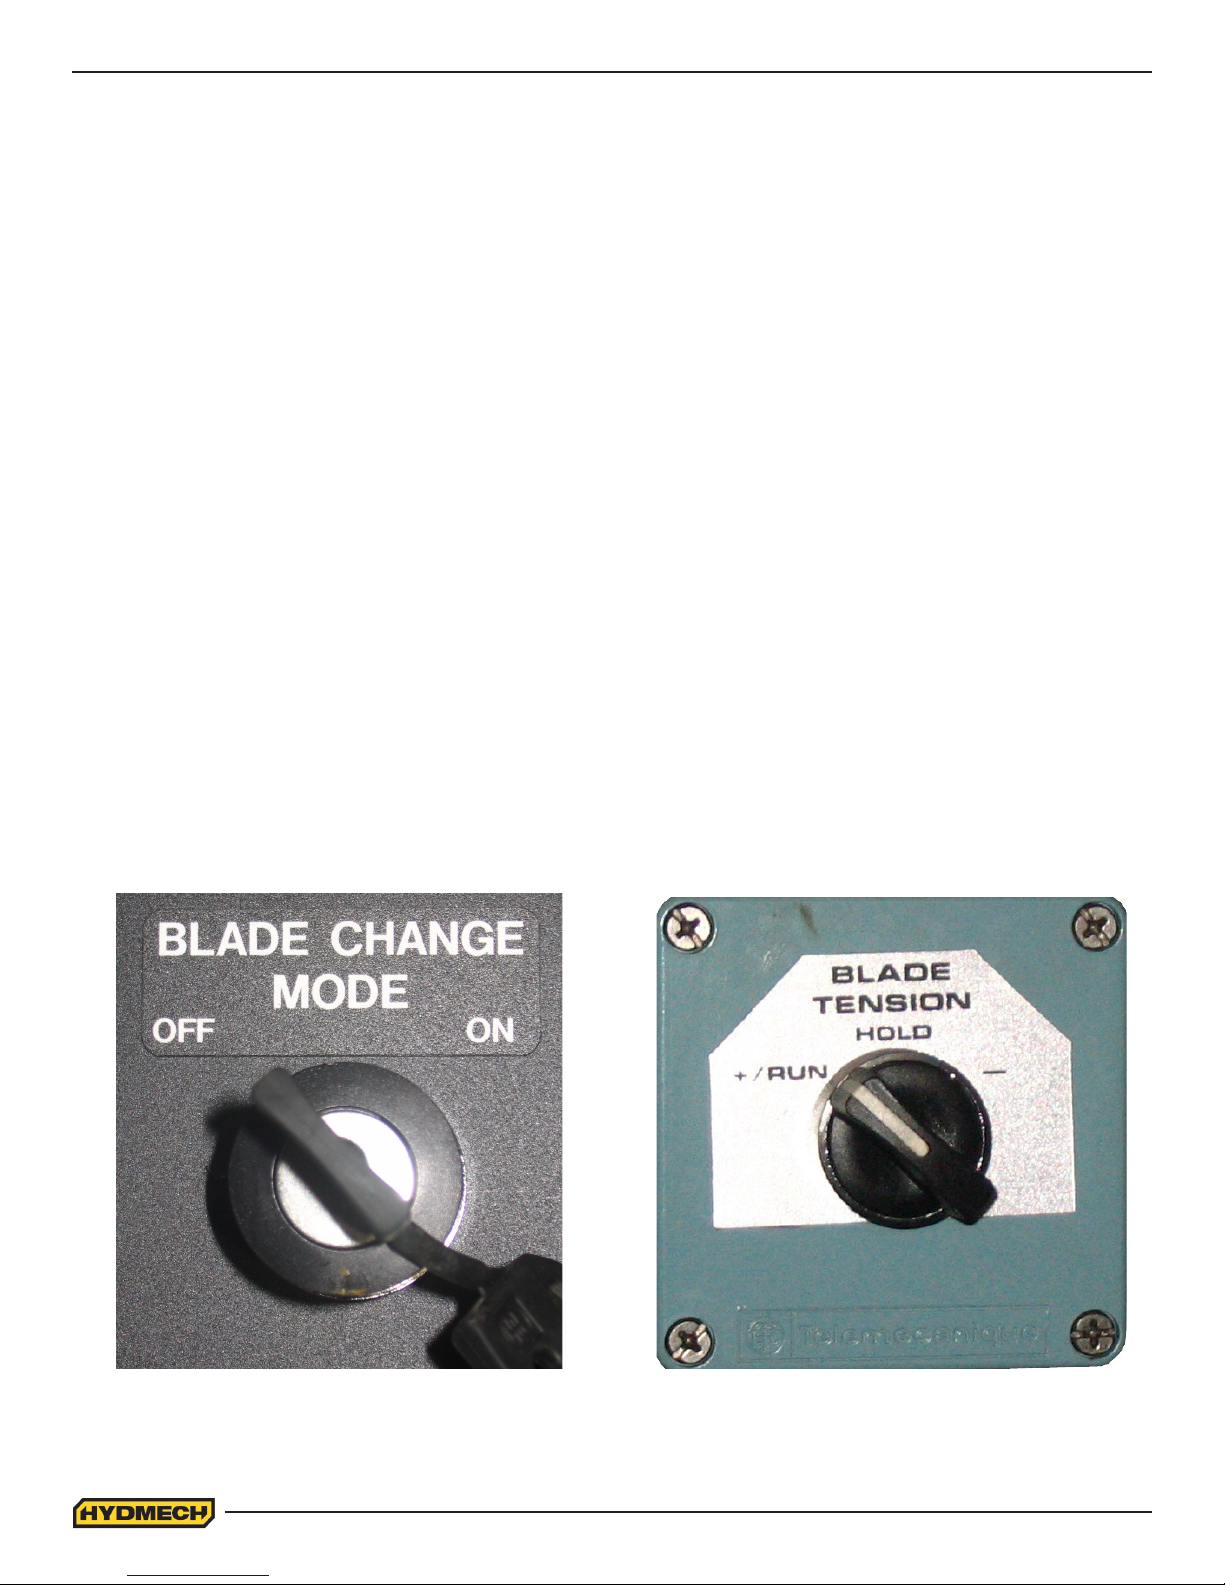
Located in the idler wheel box, is a three position maintained switch: Normal running position is
+/RUN. This position will keep constant tension on the blade. In the center HOLD position the
idler wheel is held in position with not tension applied to the blade. The “-“ position retracts the
idler wheel, releasing blade tension and allowing for blade removal.
DISPLAY
The following information is displayed on the E1012 HMI:
1. Head Height. (Inches)
2. Feed Rate. (Inches/minute)
3. Blade Speed. (surface feet/minute)
4. Cutting Time Elapsed.
5. Cut Time Remaining.
(Before Head Down switch is activated)
2.4
Page 22
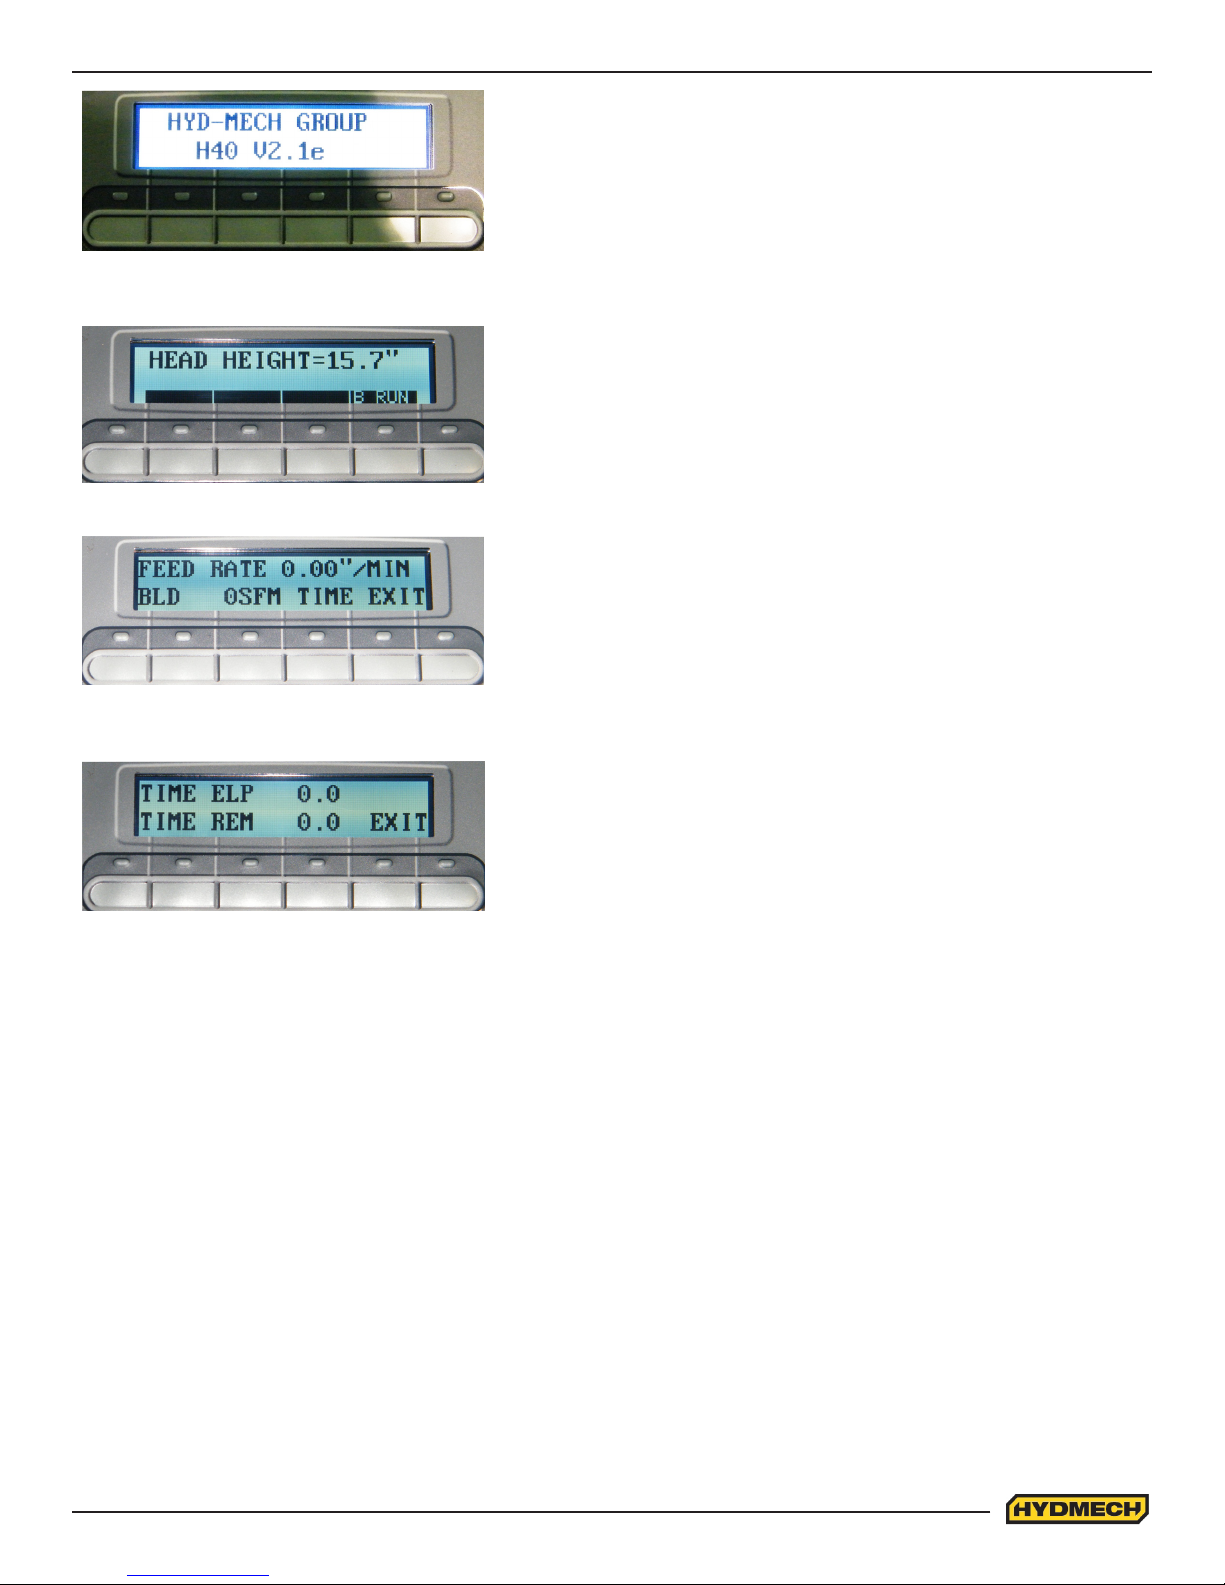
When the machine is initially powered the LCD will show company logo and software version. On activation of a push
button or selector switch the LCD display will show the head height.
Depressing the button under B RUN will change the screen to show FEED RATE and BLADE SPEED.
Depressing the button under TIME will change the screen to show CUTTING TIMES.
Depressing the button under EXIT will change the display to the previous screen.
2.5
Page 23
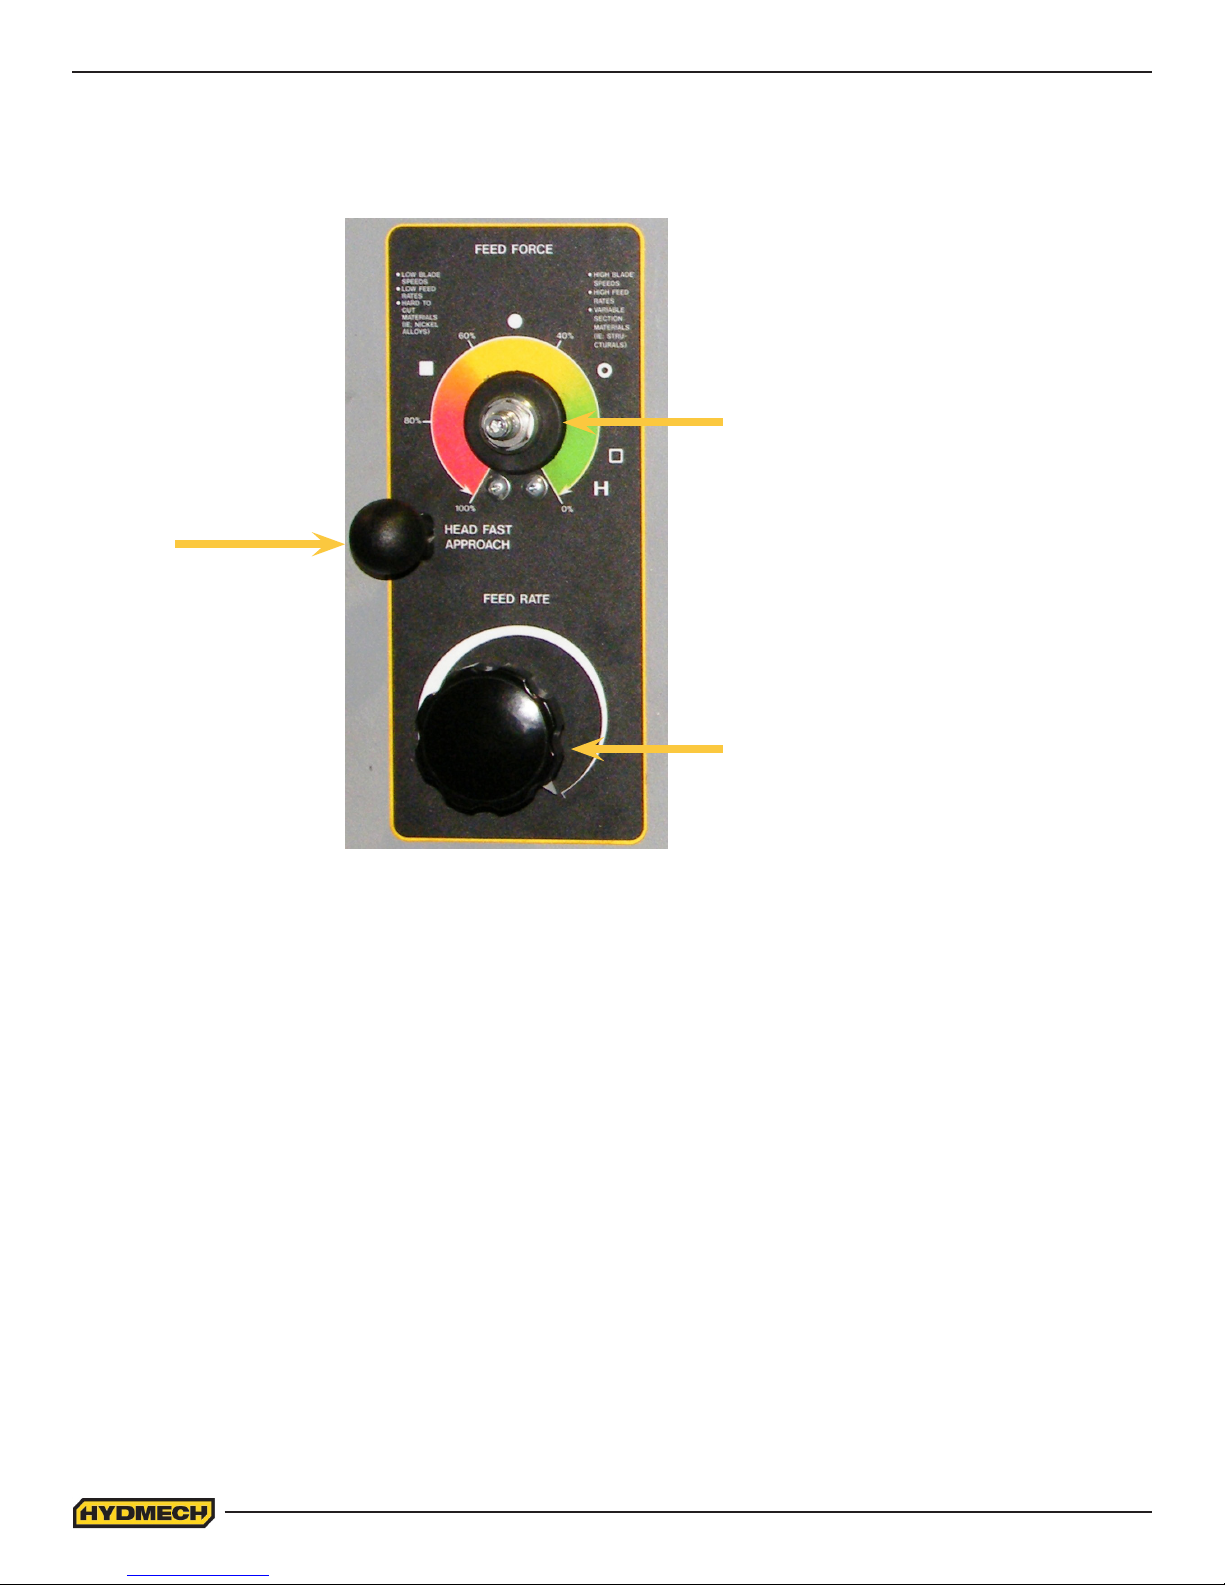
HYDRAULIC FEED CONTROL
The Hydraulic Feed Control is located to the left of the control panel. These controls allow independent control of
Feed Force (FF) and Feed Rate (FR)
FEED FORCE IS FACTORY PRESET
AND CANNOT BE ADJUSTED ON ANY
H40 MODEL.
FAST APPROACH LEVER.
DEPRESS FOR FAST HEAD
DESCENT
FEED RATE KNOB
USED TO SET FEED RATE
(COUNTERCLOCKWISE
ROTATION TO INCREASE AND
CLOCKWISE ROTATION TO
DECREASE).
2.6
Page 24
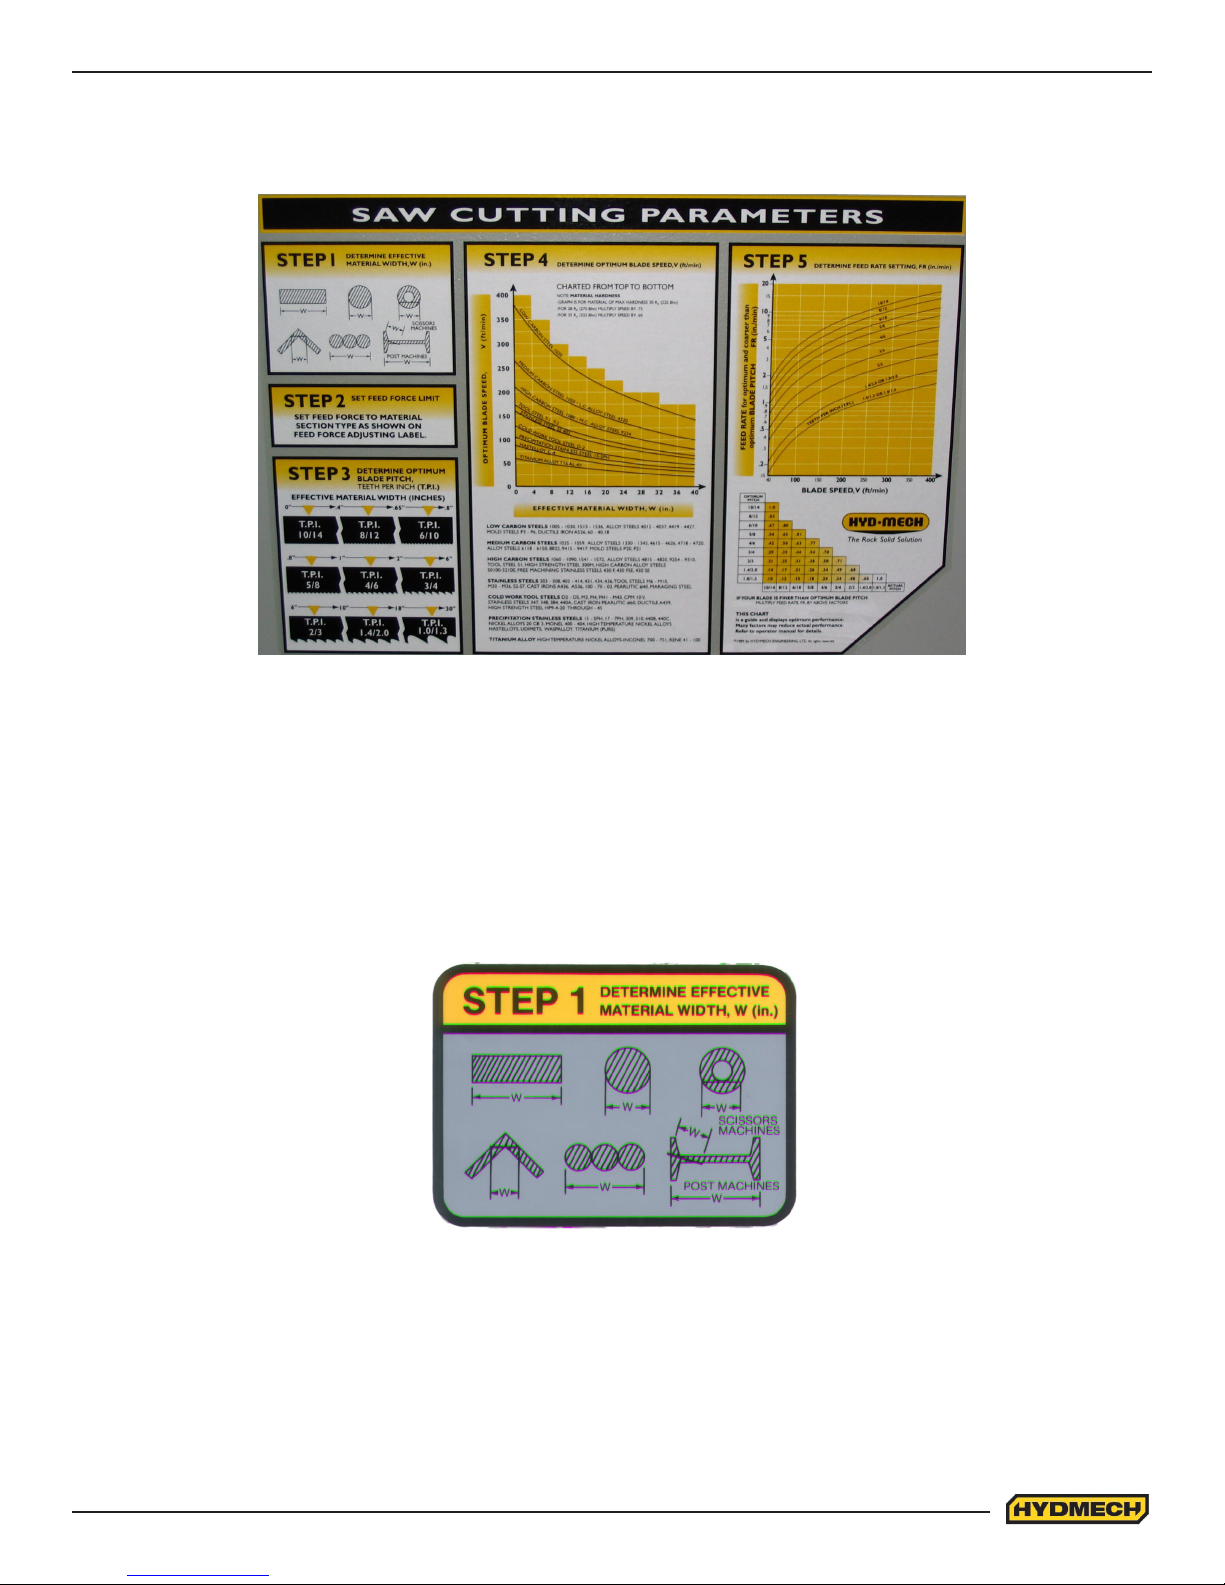
CUTTING PARAMETERS CHART
A full size CUTTING PARAMETERS CHART is mounted on the front of the saw. The chart contains ve steps for the
operator to follow in order to achieve optimum performance of the saw. These steps are detailed on the following pages.
Saw Cutting Parameters Chart
CHART EXAMPLE #1
We will use the parameters chart to set up the saw for cutting 8” (200mm) Diameter #1045 Carbon Steel.
STEP 1: DETERMINE EFFECTIVE MATERIAL WIDTH - W (inches) or (mm)
Eective material width, W (in.) for most common shapes of materials, is the widest solid part of the material to be in
contact with blade during cutting. For simple shapes, as illustrated on the chart, this can be directly measured. For
bundles of tubes and structurals, measuring the eective width is dicult. Eective width is 60% to 75% of the actual
material width.
Material Width Chart
NOTES:
1. Eective material width, as determined here in STEP 1, can be thought of as the average width of material “seen”
by each tooth, and it is used in STEPS 3 and 4.
In Example #1, for an 8” (200 mm) diameter solid, Eective Material Width is 8” (200mm).
2.7
Page 25
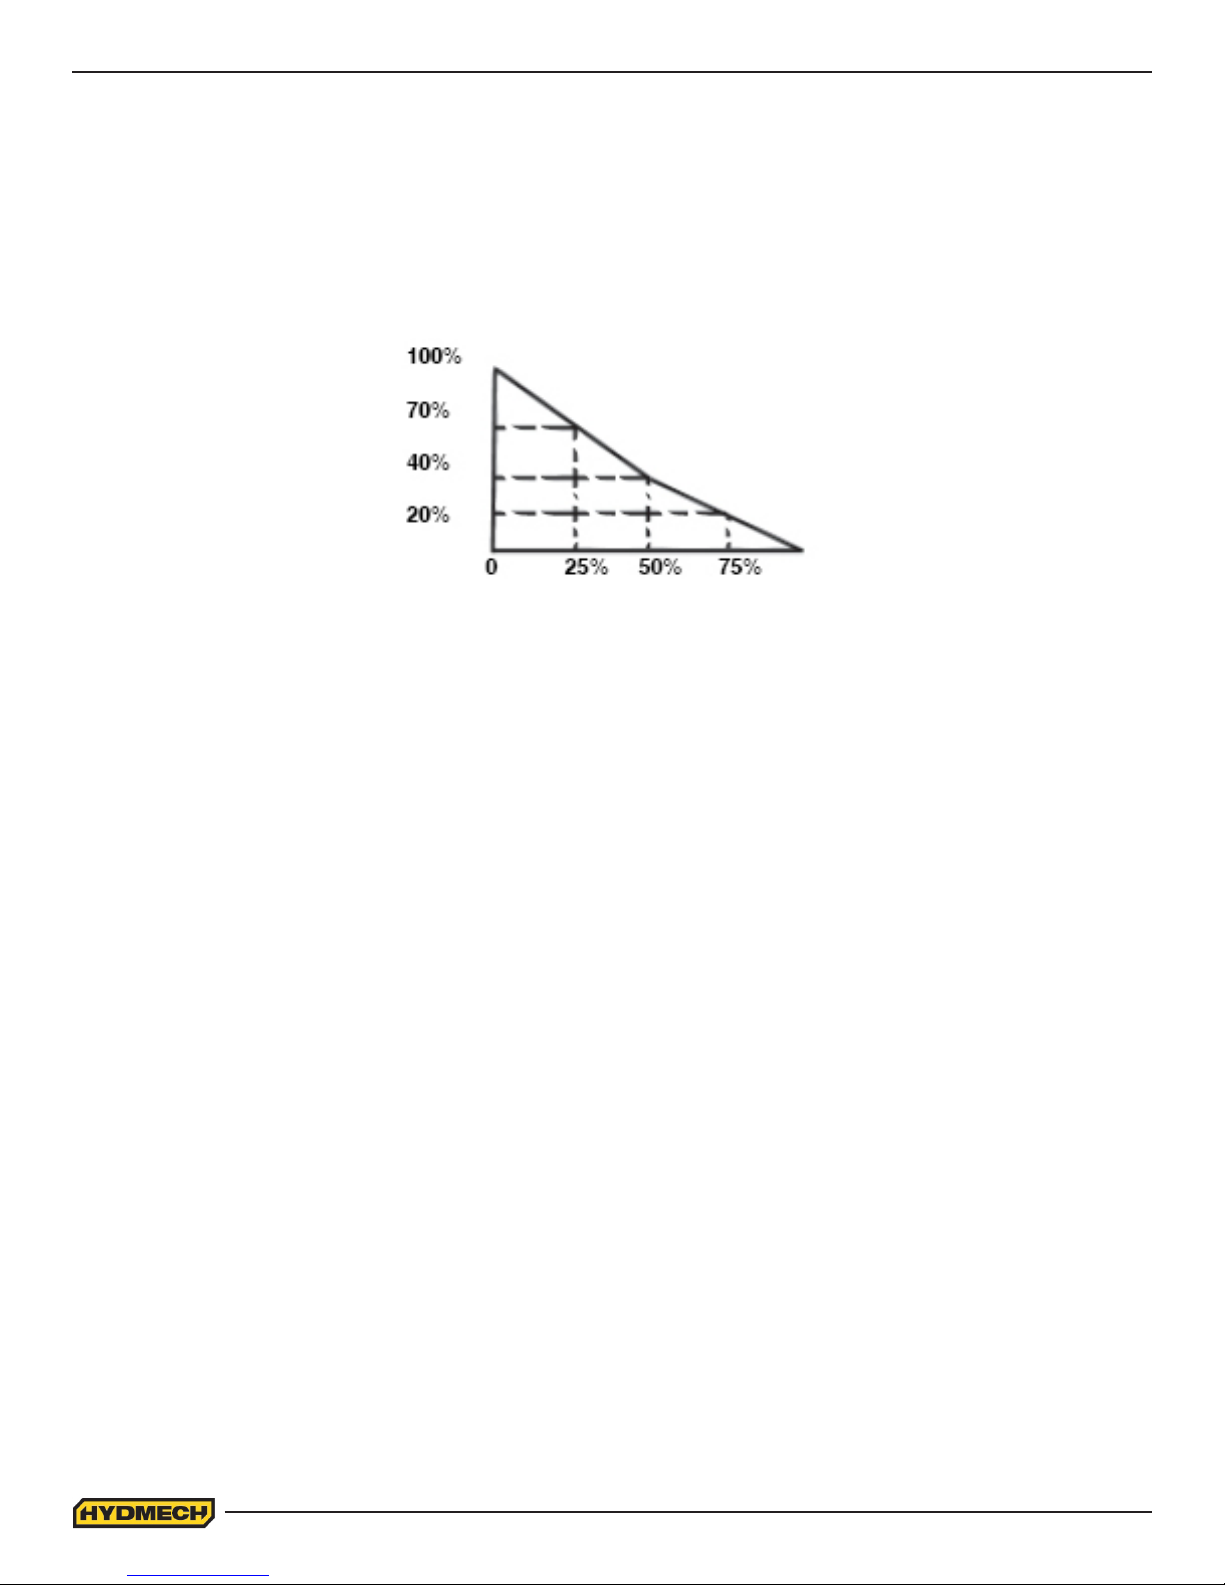
STEP 2: SET FEED FORCE LIMIT (DOES NOT APPLY TO H40 MACHINES AS FEED FORCE IS FACTORY PRESET)
The Feed Force Limit is the maximum amount of force with which the head is allowed to push the blade into the
work-piece.
CUTTING SOLIDS
For cutting solids, the wider the section, the less FF should be set, to avoid blade overloading. See the graph below.
% OF FF
SETTING
(INDICATED
ON LABEL)
MAT’L WIDTH AS %
OF SAW CAPACITY
EXAMPLE: When cutting a solid which is 1/2 of machine capacity using the graph, locate 50% on the horizontal line and
travel upwards to the plotted line and then travel directly across to the vertical FF Setting line. The point that you have
arrived at shows a setting of 40% for a piece 50% of capacity.
CUTTING STRUCTURALS: A reduced Feed Force Setting is used when cutting structurals.
2.8
Page 26
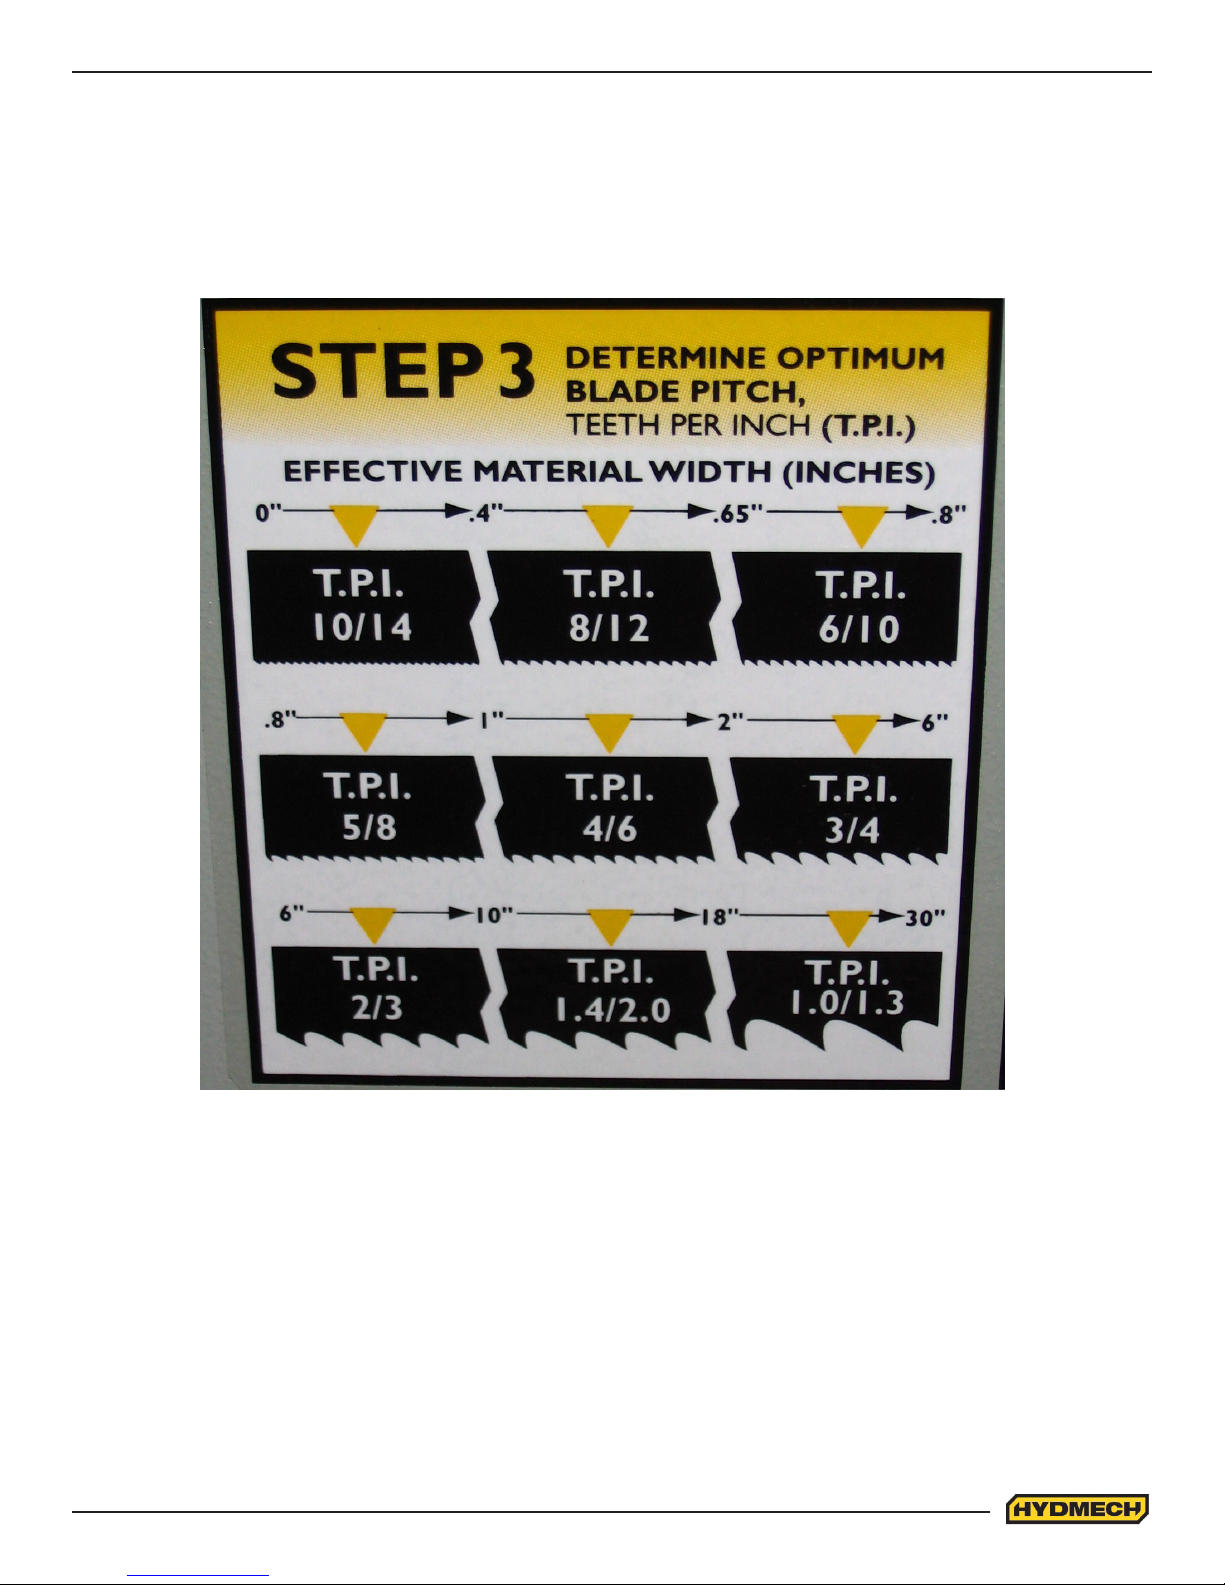
STEP 3: DETERMINE OPTIMUM BLADE PITCH - TEETH PER INCH (T.P.I.)
Selecting a blade with proper tooth pitch is important in order to achieve optimal cutting rates and good blade life.
For cutting narrow or thin wall structural materials a ne blade with many teeth per inch (T.P.I.) is recommended. For wide
materials a blade with a coarse pitch should be used. The sketch can be referenced for the blade pitch changes for
diering eective material widths.
Optimum Blade Pitch (T.P.I) for Material Width (Inches)
It is impractical to change the blade to the proper pitch every time a dierent width of material is cut and it is not
necessary, but remember that the optimum blade will cut most eciently. Too ne a blade must be fed slower on wide
material because the small gullets between the teeth will get packed with chips before they get across and out of the cut.
Too coarse a blade must be fed slower because it has fewer teeth cutting and there is a limit to the depth of a cut taken by
each tooth. Allowance for the use of a non-optimum blade is made in STEP 5.
Example #1: Eective material width of 8” (200 mm):
Optimum blade has 2/3 teeth per inch.
2.9
Page 27
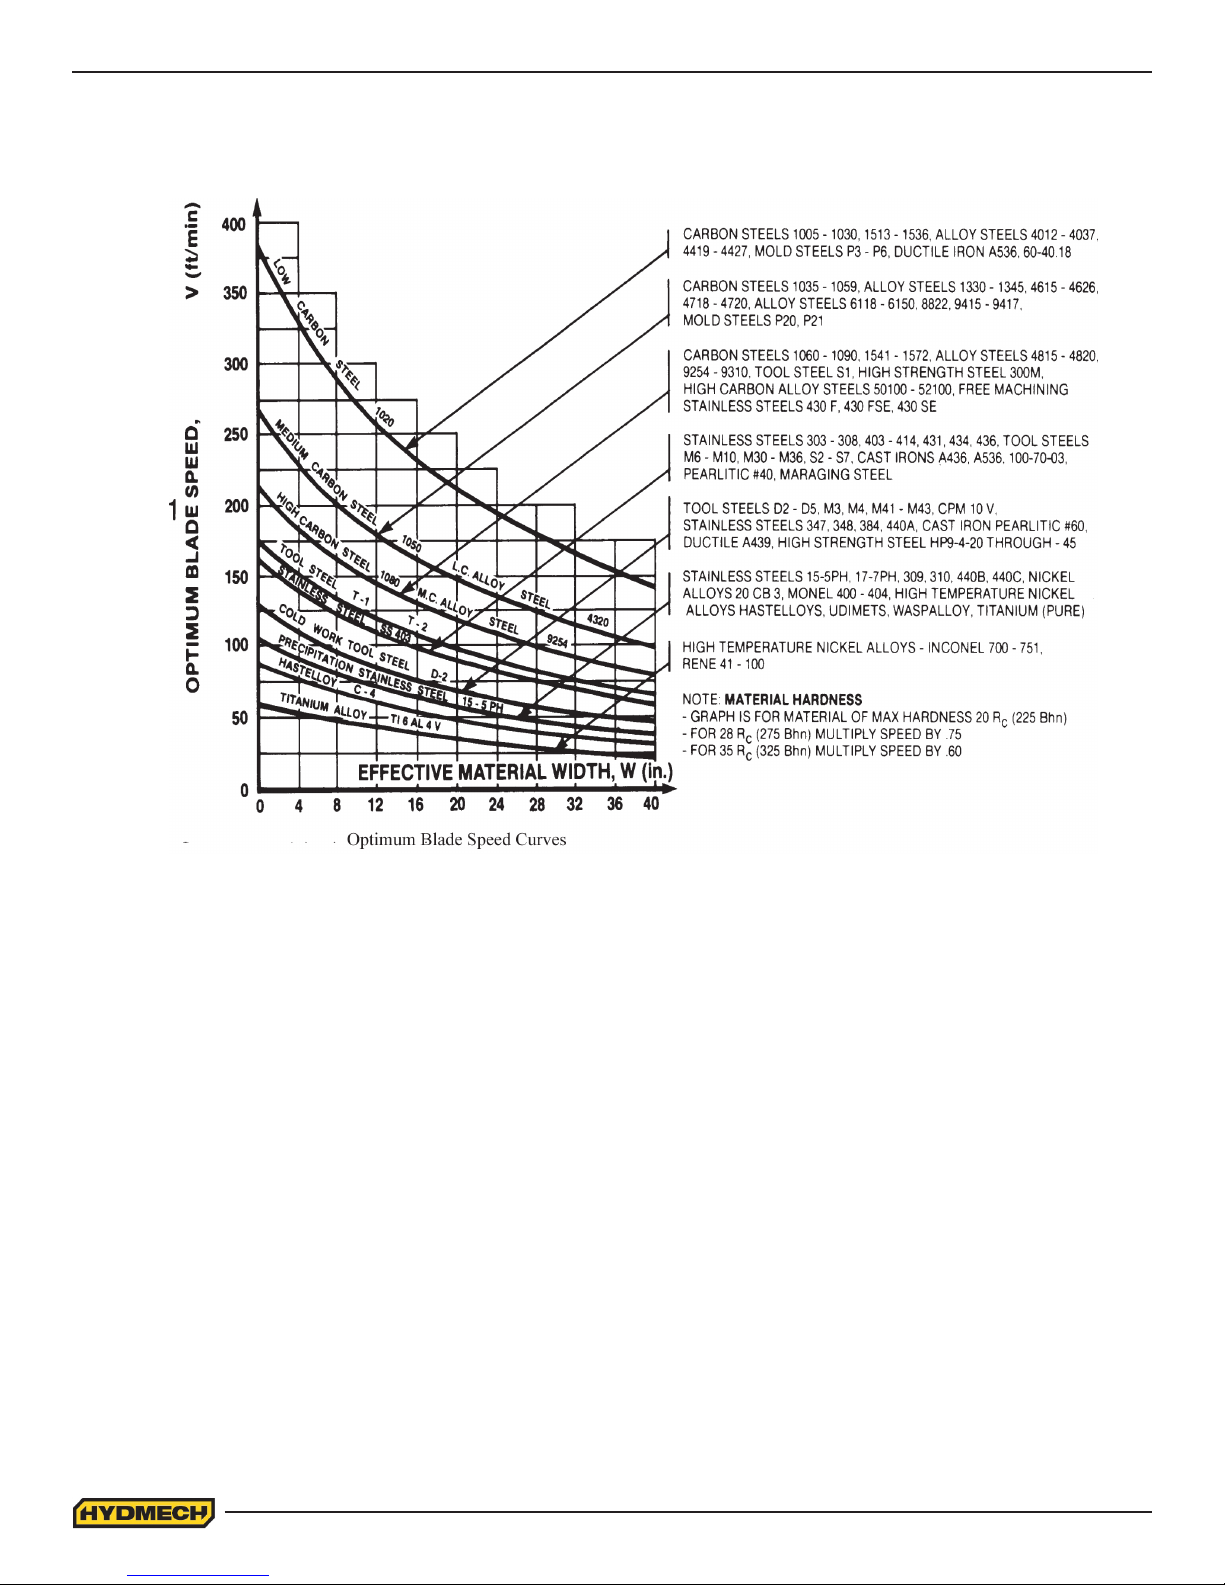
STEP 4: DETERMINE OPTIMUM BLADE SPEED, V (ft/min) (m/min)
The relationship between optimum blade speed and eective material width for various materials is represented on the
graph shown.
The graph shows that as eective material width gets wider or as material gets harder, lower blade speeds are recommended. If material is narrow or soft, higher blades speeds should be selected.
Example #1
1. 8” (200mm) diameter #1045 Medium Carbon Steel solid bar is to be cut.
2. On the graph above nd the Medium Carbon Steel Curve which represents the optimum blade speeds for 1045
Carbon Steel.
3. On the horizontal axis (eective material width axis) nd number 8 which represents eective material width of an
8” (200mm) diameter solid.
4. Find the point where a vertical line from 8” (200mm) intersects the Medium Carbon Steel Curve.
5. From this intersection point run horizontally left to the vertical axis (optimum blade speed axis) and nd the point
marked “200”.
6. For 8” (200mm) diameter, 1045 Carbon Steel solid bar 200 ft/min (60m/min) is the optimum blade speed.
NOTE:
1. Higher than optimum blade speed will cause rapid blade dulling. Lower than optimum blade speeds reduce
cutting rates proportionately and do not result in signicantly longer blade life except where there is a vibration
problem. If the blade vibrates appreciably at optimum speed as most often occurs with structurals and bundles, a
lower blade speed may reduce vibration and prevent premature blade failure.
2. Material Hardness - The graph above illustrates blade speed curves for materials of hardness 20 RC (225 Bhn) or
lower. If the material is hardened then the multipliers need to be used. These multipliers are given in the NOTE at
the bottom right of the graph. As the hardness increases the optimum blade speed decreases.
2.10
Page 28
The following table gives examples of the optimum blade speeds for dierent materials.
# MATERIALS OPTIMUM BLADE SPEED
(ft/min) (m/min)
1 5” (125mm) Diameter Solid Carbon Steel 225 70
2 12” (300mm) I-Beam 290 90
3 4” x 4” (100mm x 100mm) Rect. Tube 1/4” (6mm) Wall 350 110
4 4” (100mm) 400 Stainless Steel 140 45
5 2” x 2” (50mm x 50mm) Rect. Tube 1/4” (6mm) Wall
Bundle 5” x 5” pcs. 10” x 10” (500mm x 500mm) 325 100
6 3” x 3” (75mm x 75mm) Inconel 60 20
Materials and Blade Speed
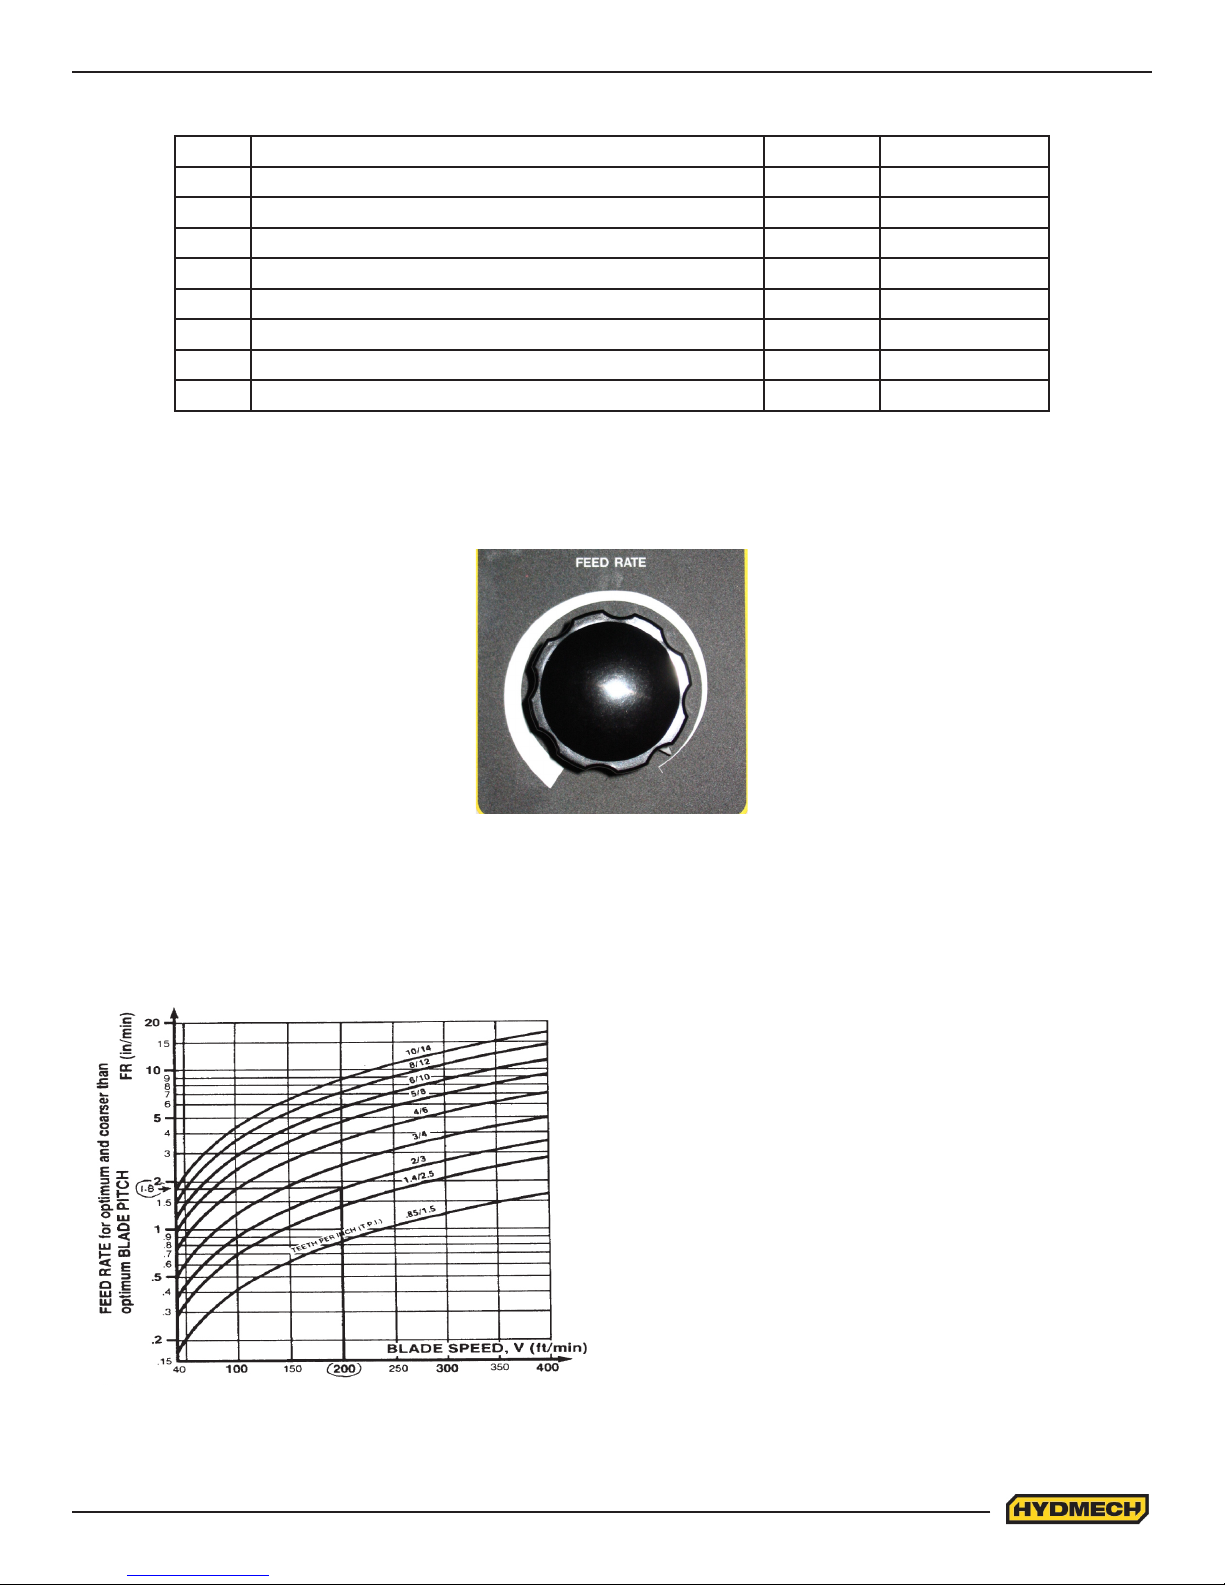
STEP 5: DETERMINE FEED RATE SETTING, FR (in/min) (mm/min).
FEED RATE is the vertical speed at which the blade descends through the work-piece.
The FEED RATE Knob controls FEED RATE of the blade descent. The FEED RATE should be adjusted only in one direction (from “O” to required value). If you go too far, go back to “O” and come back up. To set FEED RATE for particular
cutting situations use the graph below, which represents the relationship
between FEED RATE, blade speed and blade pitch.
Example #1: It is known from Step 3 that optimum blade
pitch is 2/3, and from Step 4 that blade speed is 200 ft/min
(60mm/min). From the Graph on the left, the FEED RATE is
determined in the following way:
1. On the horizontal axis (blade speed axis), nd
200 ft/min (60mm/min).
2. Find the point where a ver tical line from 200 ft/min
(60mm/min) would intersect the 2/3 blade pitch curve
3. From this intersection point run horizontally left to the
ver tical (FEED RATE) axis, to ar rive at 1.8 in/min
(45mm/min) FEED RATE. Thus 1.8 in/min (45mm/min)
is the FEED RATE for cutting 8” (200mm) diameter 1045
Carbon Steel when the optimum 2/3 pitch blade is used.
Feed Rate Calculation
2.11
Page 29
FEED RATE, continued
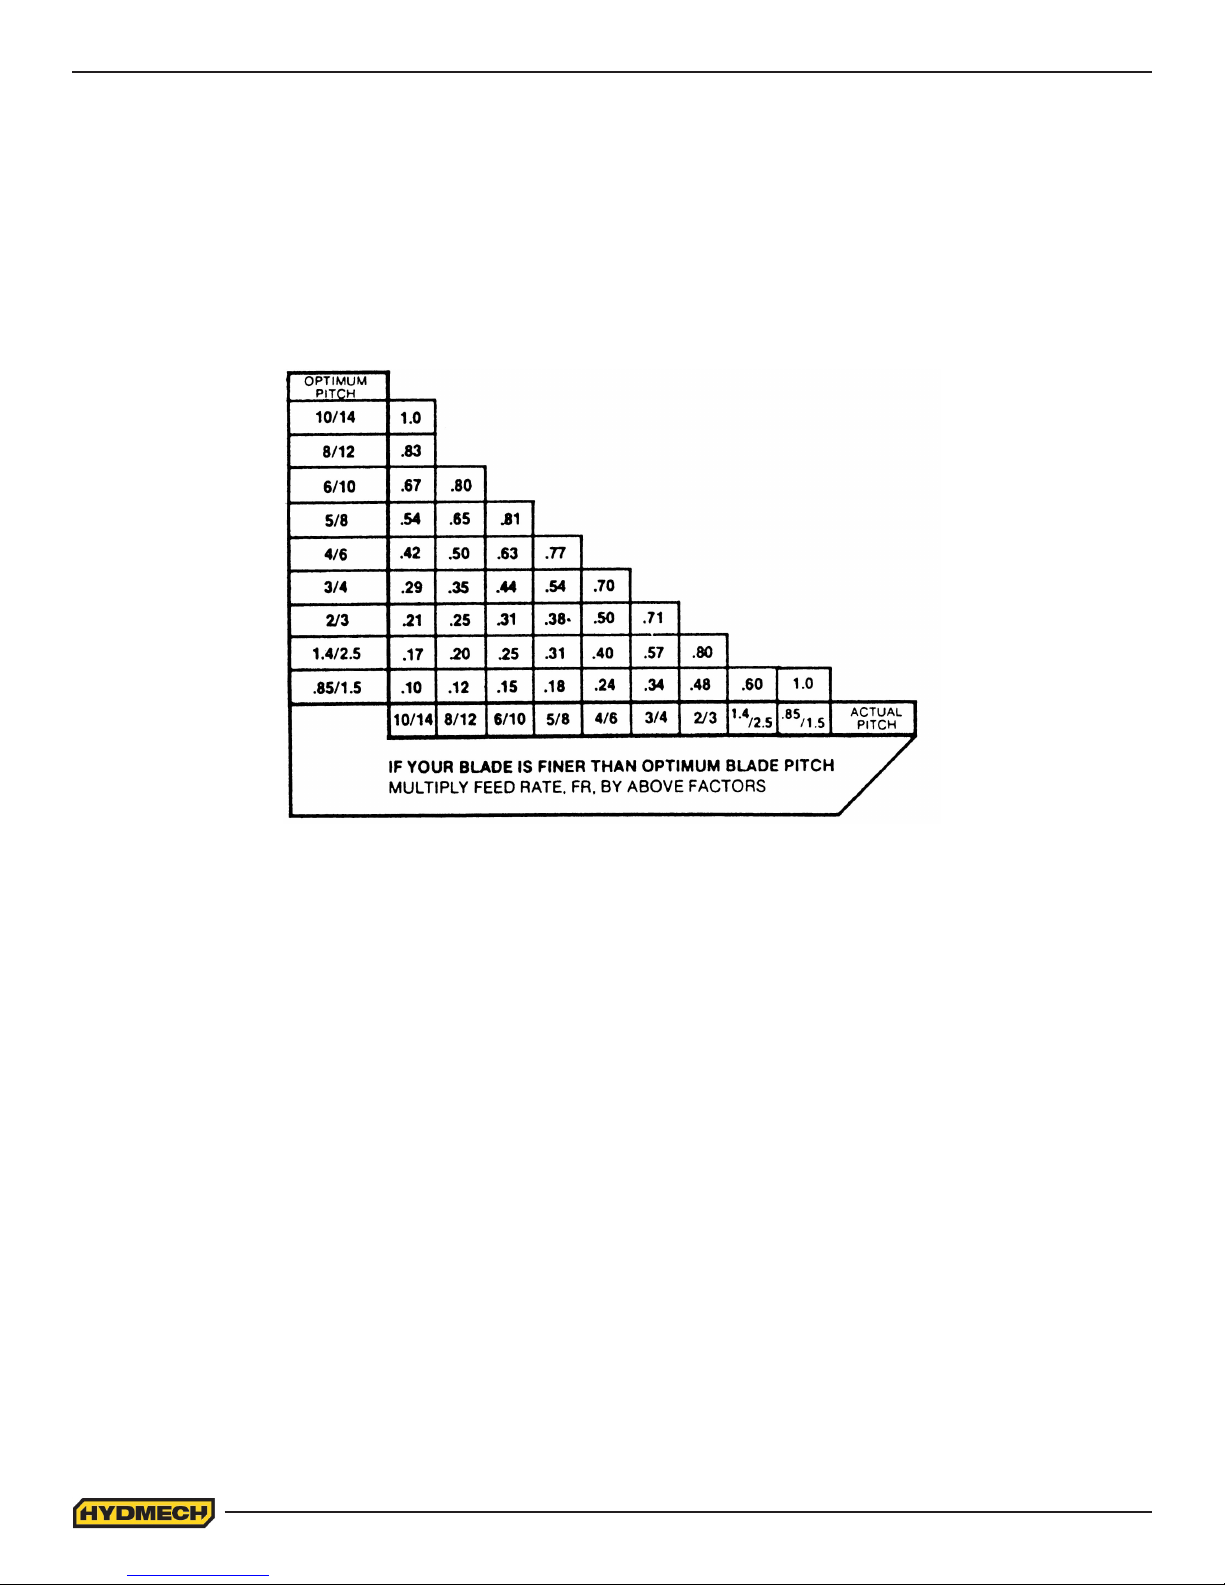
If the saw is tted with a blade coarser than optimum (e.g.: 1.4/2.5 TPI) we can still use the graph, but we go to the 1.4/2.5
curve. As a result we nd that the FEED RATE is decreased to 1.3 in/min (133mm/min) for this blade. If however, the
machine is tted with a ner than optimum blade (e.g. 3/4 TPI) we use the graph for the optimum blade as before, and
then use a multiplier given by the table below.
Optimum Vs Actual Blade Pitch
ADDITIONAL CUTTING SETUP EXAMPLES
EXAMPLE # 2
Material:
Round Steel Tube SAE 4320 - Hardened to 35 RC (325 Bhn )
Dimensions - 6” O.D. x 4” I.D. (150mm O.D. x 100mm I.D.)
Step 1 Eective Material Width: 4 1/2” (.75 X 6) 114mm (19 x 6)
Step 2 Feed Force limit setting for 6” Diameter material (Refer to Feed Force Limit, Setting in Step 2)
Step 3 Optimum blade pitch (TPI): 3/4 T. P. I.
Actual blade pitch on the saw: 4/6 T. P. I.
Step 4 Optimum blade speed for 4 1/2” eective 225 ft/min (70m/min) material width
Blade speed reduced by hardness factor: 225 ft/min X .60 = 135ft/min (70m/min x .60 = 42m/min)
Step 5 Feed Rate for 3/4 TPI blade: 1.8 in/min (45mm/min)
Feed Rate for 4/6 TPI blade: 1.8 in/min X .70 = 1.3in/min
(reduced by ner than optimum blade pitch factor) (45mm/min x .70= 31.5mm/min)
2.12
Page 30
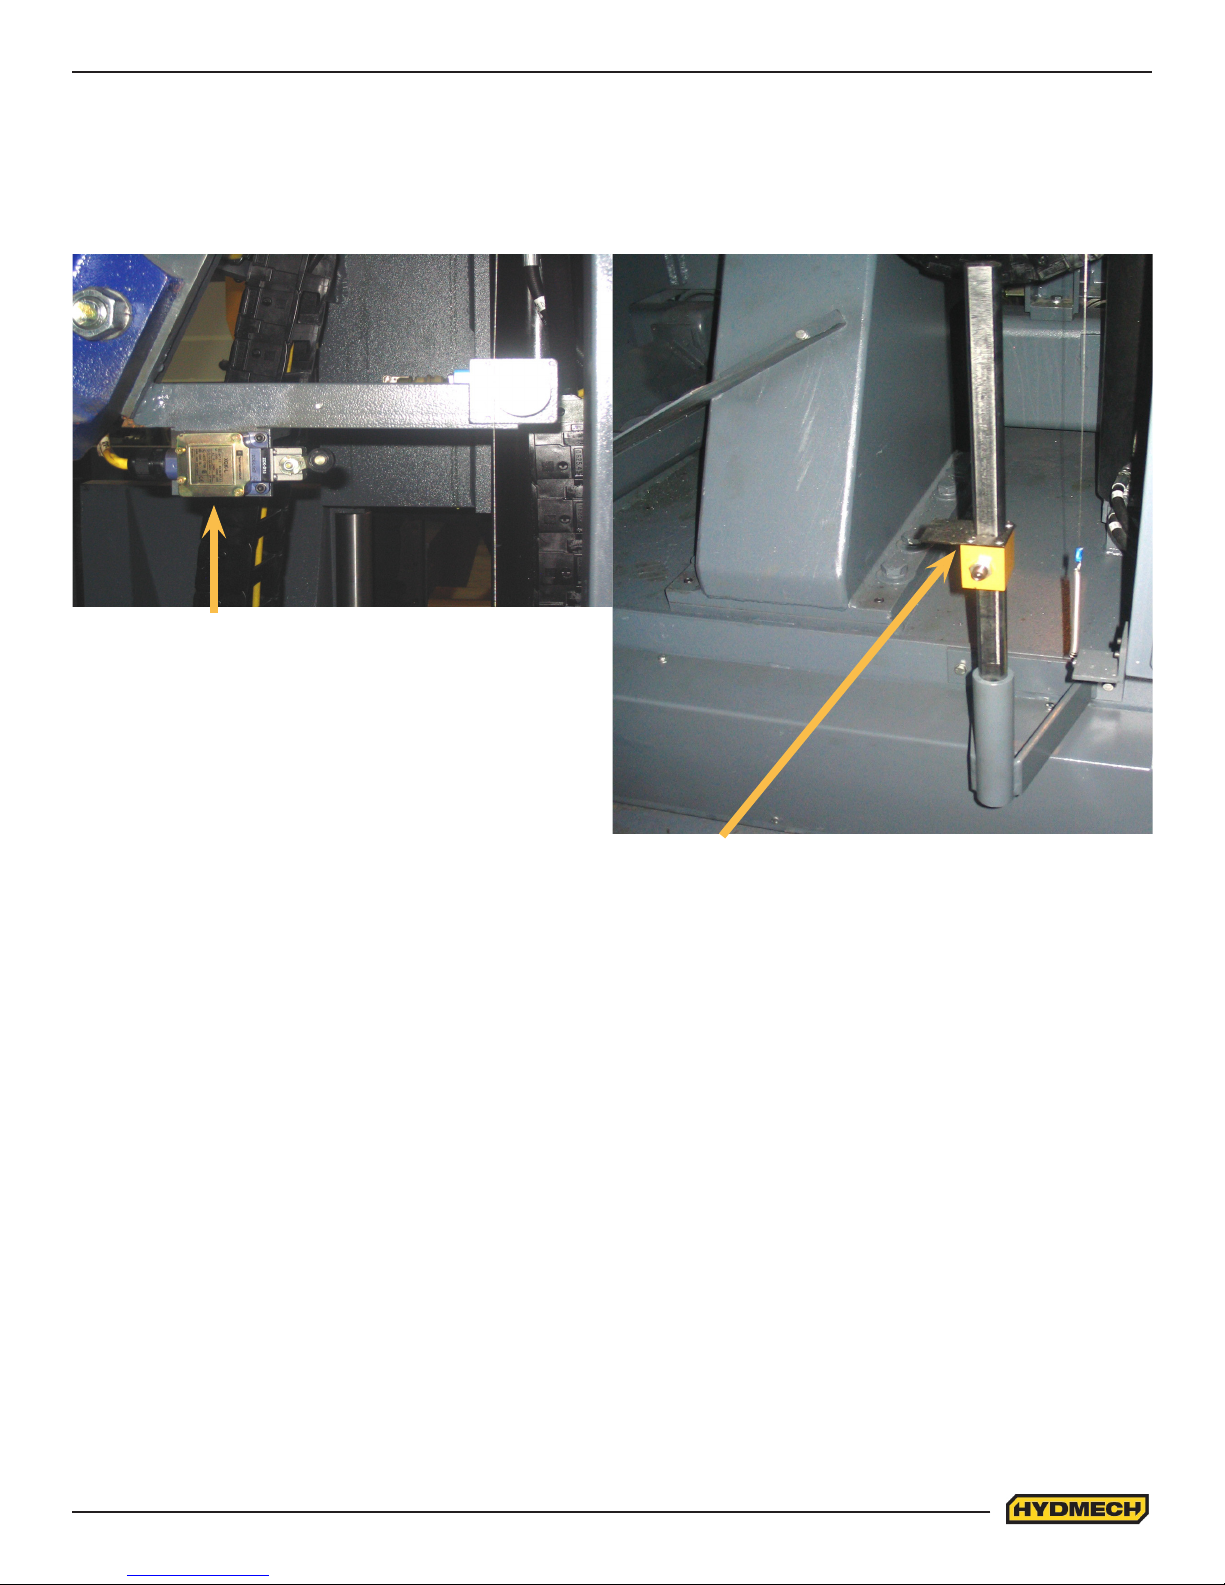
HEAD DOWN LIMIT SETTING
HEAD DOWN LIMIT SETTING
Head Down Limit: This limit is factory set and under ordinary cutting requirements should not be changed. If changed, it
may cause the machine to malfunction in the automatic cycle.
Head Down Limit: This limit is factory set and under ordinary cutting requirements should not be changed. If changed, it
may cause the machine to malfunction in the automatic cycle.
LIMIT SWITCH
HEAD DOWN ADJUSTMENT BLOCK
2.13
Page 31
GUIDE ARM POSITIONING
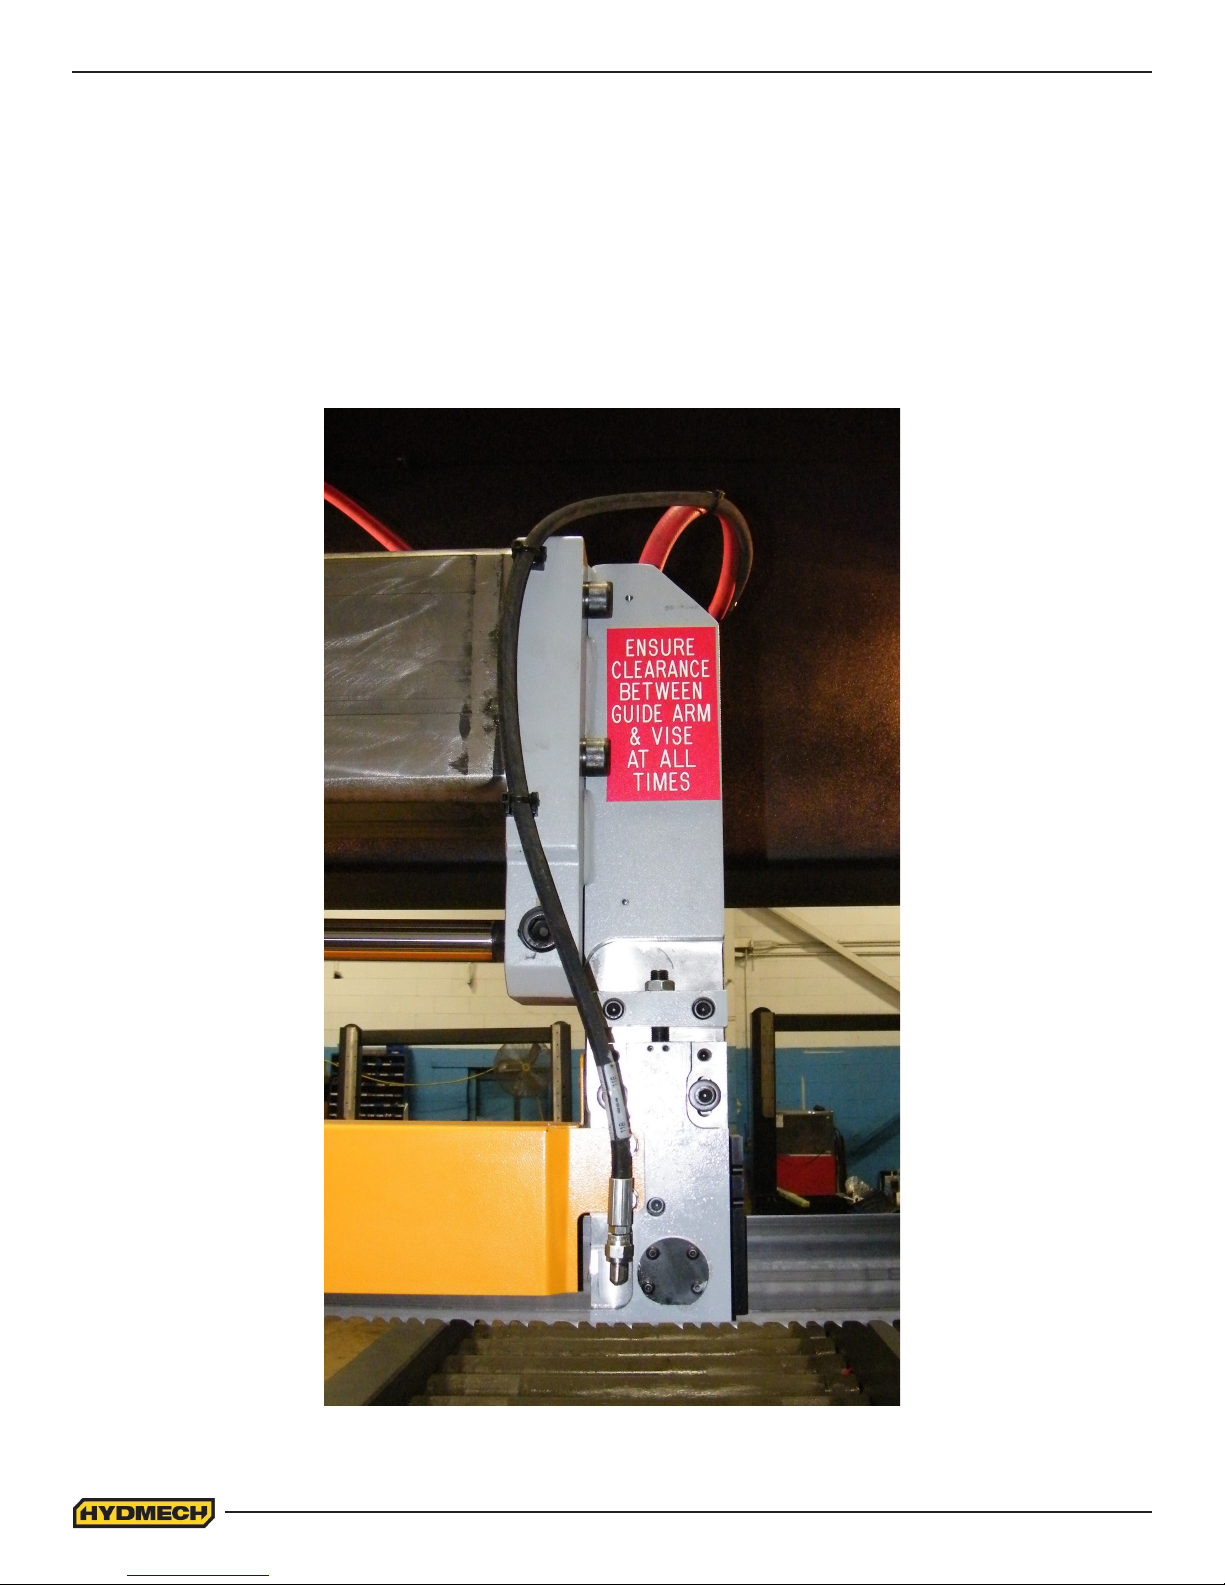
The adjustable guide arm should always be adjusted with respect to the material width. It will optimize cutting
conditions and increase blade life with the guide arm adjusted as close to the material as permitted.
In order to adjust the guide arm, the remote guide arm adjustment switch, located on the control console is
used to hydraulically position the guide arm. Turn the switch clockwise to move the guide arm toward the stock.
Turn the switch counter clockwise to move the guide arm away from the stock.
ENSURE CLEARANCE BETWEEN GUIDE ARM AND VISES AT ALL TIMES.
H-40 Guide Arm Position
2.14
Page 32
COOLANT CONTROLS
GUIDE ARM
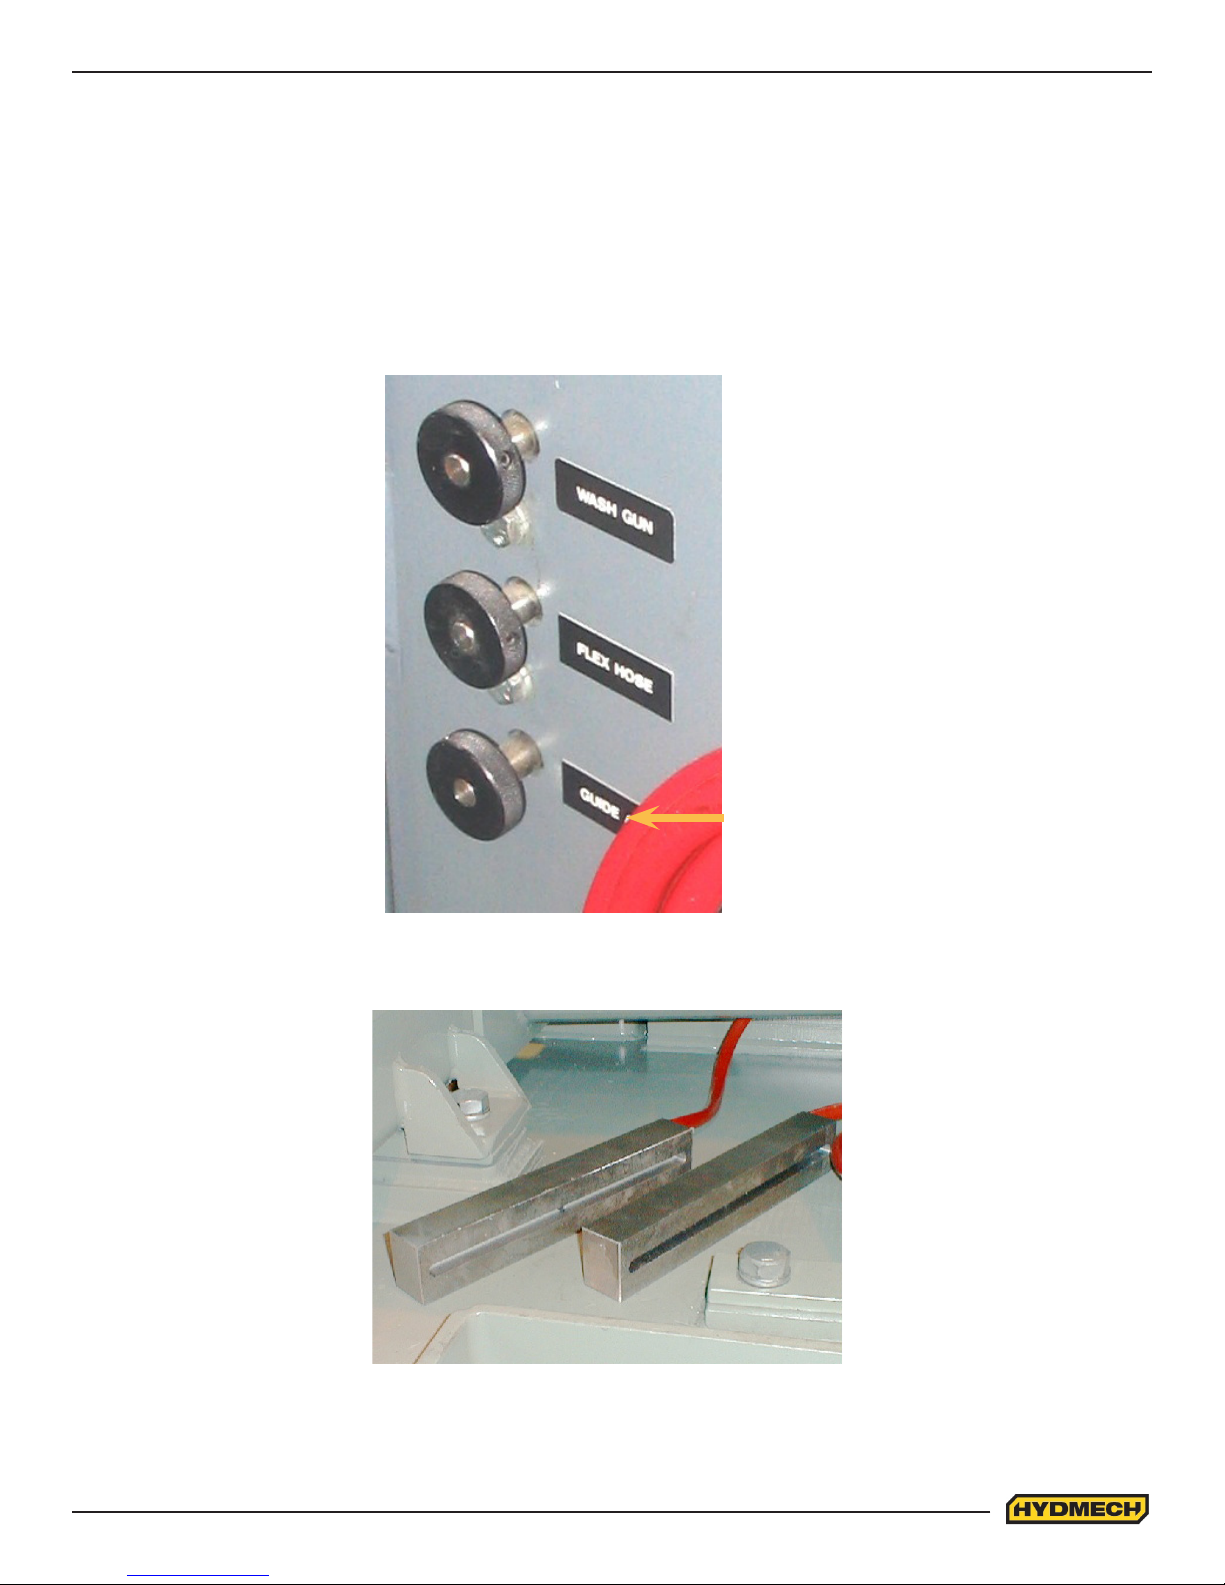
A generous ow of coolant should be applied in order to increase production and blade life. The machine is provided with
adjustable coolant on the left side of the operator panel as shown below.
A properly adjusted ow of coolant should cover the blade (from the adjustable guide arm) which in turn will carry it into
the cutting area. Additional coolant can be supplied with the coolant bars shown below which are controlled by the knob
labeled ‘FLEX HOSE”.
NOTE: When cutting materials that do not need coolant (cast iron), some coolant ow is required to provide blade
lubrication and prevent scoring of the blade by the carbides.
GUIDE ARM
Coolant ow controls, found on left side of control console
Coolant Bars can be placed on top of materials for extra coolant
coverage. Flow is controlled with the knob labeled “FLEX HOSE”
2.15
Page 33
SECTION 3 – MAINTENANCE
SAFETY DURING MAINTENANCE AND TROUBLESHOOTING
“Lock-out”, or “Lock-out Tag-out” are terms that refer to procedures taken to prevent the unexpected start-up, or other release of energy, by a machine, whenever anyone is required to remove or bypass safety guards or devices, or whenever
anyone is required to place part of his body in a hazard area.
In almost all jurisdictions, it is required that owners of industrial equipment establish and post lock-out procedures. Know
and use the lock-out procedures of your company or organization. In the absence, of such posted procedures, use the
following procedure.
LOCK OUT PROCEDURE
Whenever work is to be performed on a machine, which requires removal or bypassing of safety guards or devices, or the
placement of part of anyone’s body in a hazard area, the following steps shall be taken:
1. Operator shuts down the machine.
2. The supervisor in charge of the machine must be informed of the intention to Lock-out the machine.
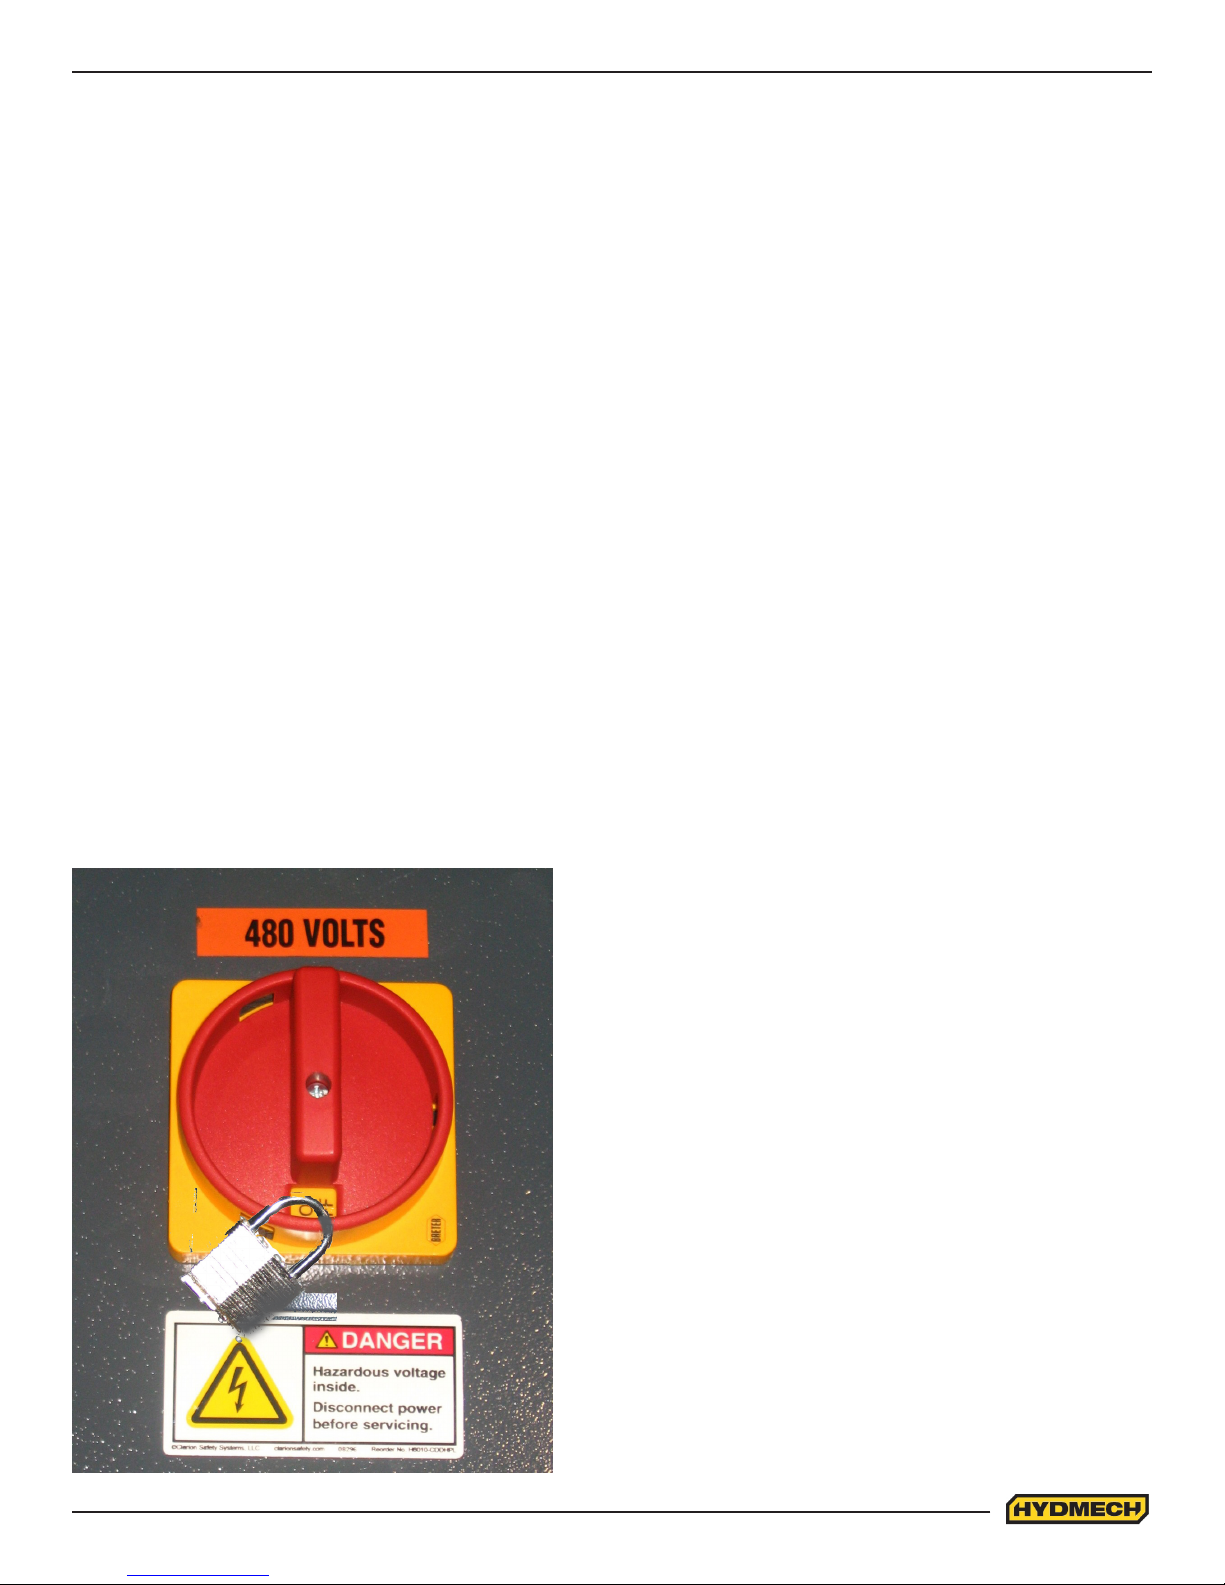
3. The FEEDER power which supplies power to the machine and which is connected to the machine via the Power
Junction Box (see picture below) must be turned OFF and locked in the OFF (0) position by means of a padlock.
The key for this padlock must be kept by the person performing the work on the machine. If more than one person
is performing work on the machine, then a multiple lock hasp shall be used, and each person shall apply his or her
own lock to the hasp.
4. The Machine Power Disconnect Switch must be turned OFF, and locked in the OFF (0) position by means of a
padlock. The key for this padlock must be kept by the person performing the work on the machine. If more than one
person is performing work on the machine, then a multiple lock hasp shall be used, and each person shall apply his
or her own lock to the hasp.
5. Prior to starting any work on the locked-out machine, the supervisor shall attempt to start the machine to ensure that
the lock-out device provides adequate protection. Operating controls must be reset to the “OFF” position after this
test.
6. Work on the locked-out machine may now proceed.
MACHINE DISCONNECT SWITCH USED FOR SAFETY
LOCKOUT PURPOSES
Machine Power Disconnect located on the door of the high
voltage electrical panel, mounted on the drive side machine
post.
1. Ensure switch is in the OFF position.
2. Install padlock and lock it.
3.1
Page 34
RESTORING MACHINE TO USE
After completion of all repairs or maintenance to the locked-out machine, it shall be restored to use as follows:
The person(s) who performed the work shall verify that all areas around the machine are safe, before the machine is
re-energized. No-one shall be permitted in un-safe areas around the machine. All guards and covers shall be properly
installed.
Each lock-out padlock shall be removed by the person who applied it.
After the lock-out padlocks are removed, and before the machine is started, the supervisor and all other employees who
use the machine, shall be informed that the lock-out has been removed. After notication is made, the machine may be
re-started.
BLADE CHANGE MODE PROCEDURE
Wear safety glasses, gloves, and a long sleeve shirt for protection when handling band saw blades during blade change.
NOTE THAT GLOVES SHOULD NEVER BE WORN NEAR A RUNNING BANDSAW BLADE. When handling new blades,
or ones that will be re-used, it is important to keep the teeth out of contact with concrete oors.
This machine is equipped with hydraulic blade tension and a ‘Blade Change Mode’ key switch, located on the operator
control panel.
This key has two positions:
OFF – All normal operations of the band saw are operative.
ON – Hydraulic motor can be started.
Blade tension is operative.
3.2
Page 35
BLADE REMOVAL
1. With the blade change mode key switch in ‘OFF’, the blade stopped and the hydraulics ON, raise the saw head
until the drive door will clear the electrical control panel.
2. Move the guide arm out to provide room between the two guide arms to easily grasp the blade with
two hands, BUT DO NOT TOUCH THE BLADE UNTIL THE BLADE CHANGE MODE SWITCH IS TURNED TO
THE ‘ON’ POSITION.
3. Turn the blade change key switch to the ‘ON’ position. The hydraulics will continue to run, but only the blade
tension switch is functional. The blade wheel doors can be opened without the hydraulics shutting down.
4. Open both blade wheel doors.
5. Release the blade tension by turning the switch briey to ‘ – ‘. By jogging the switch
between ‘HOLD’ and ‘ – ‘, it is possible to regulate the degree of tension on the blade.
6. Pull the top strand of the blade up, out of its slot above the cutting area and forward out of the slots on the inside
walls of the blade wheel housings.
7. Pull the lower strand of the blade down out of the blade guides.
8. Store and dispose of the used blade.
BLADE INSTALLATION
NOTES ABOUT NEW BLADES
• A new blade will come folded into a compact coil. Follow the blade manufacturer’s instructions for safely
unfolding the blade.
• The blade must be installed with the teeth facing towards the rear of the saw where it passes around the wheels,
and with the teeth in the cutting area pointing away the drive wheel. This may require that the blade be turned
inside out before installation.
1. With the blade change mode key switch remaining in the ‘ON’ position, turn the blade tension switch to the ‘ – ‘
position for several seconds until the idler wheel has fully retracted.
2. Insert the lower strand of the new blade into the blade guides.
3. Lift the upper strand of the blade up into its slot above the cutting area, and place it around the blade wheels.
4. Turn the blade tension switch briey to ‘ +/RUN’ and then leave it in ‘HOLD’ to retain the blade lightly on the
wheels.
5. Adjust the blade position on the wheels so that the blade is not crooked on them and the teeth overhang the back
edge of the wheels.
6. Turn the blade tension switch to ‘ +/RUN’.
7. Close both blade wheel doors.
8. Turn the blade change mode key switch to the ‘OFF’ position. The hydraulics will shut down.
9. Switch the hydraulics on, then start the blade and run for 20 seconds.
10. Stop the blade.
11. Turn the blade change key switch to the ‘ON’ position.
12. Open the blade wheel doors and inspect the blade tracking, plus the position of the blade brush. Refer to the
manual for tracking adjustments.
13. Close the blade wheel doors and turn the blade change mode key to the ‘OFF’ position.
14. Blade change procedure is now complete.
3.3
Page 36
BLADE BRUSH ADJUSTMENT
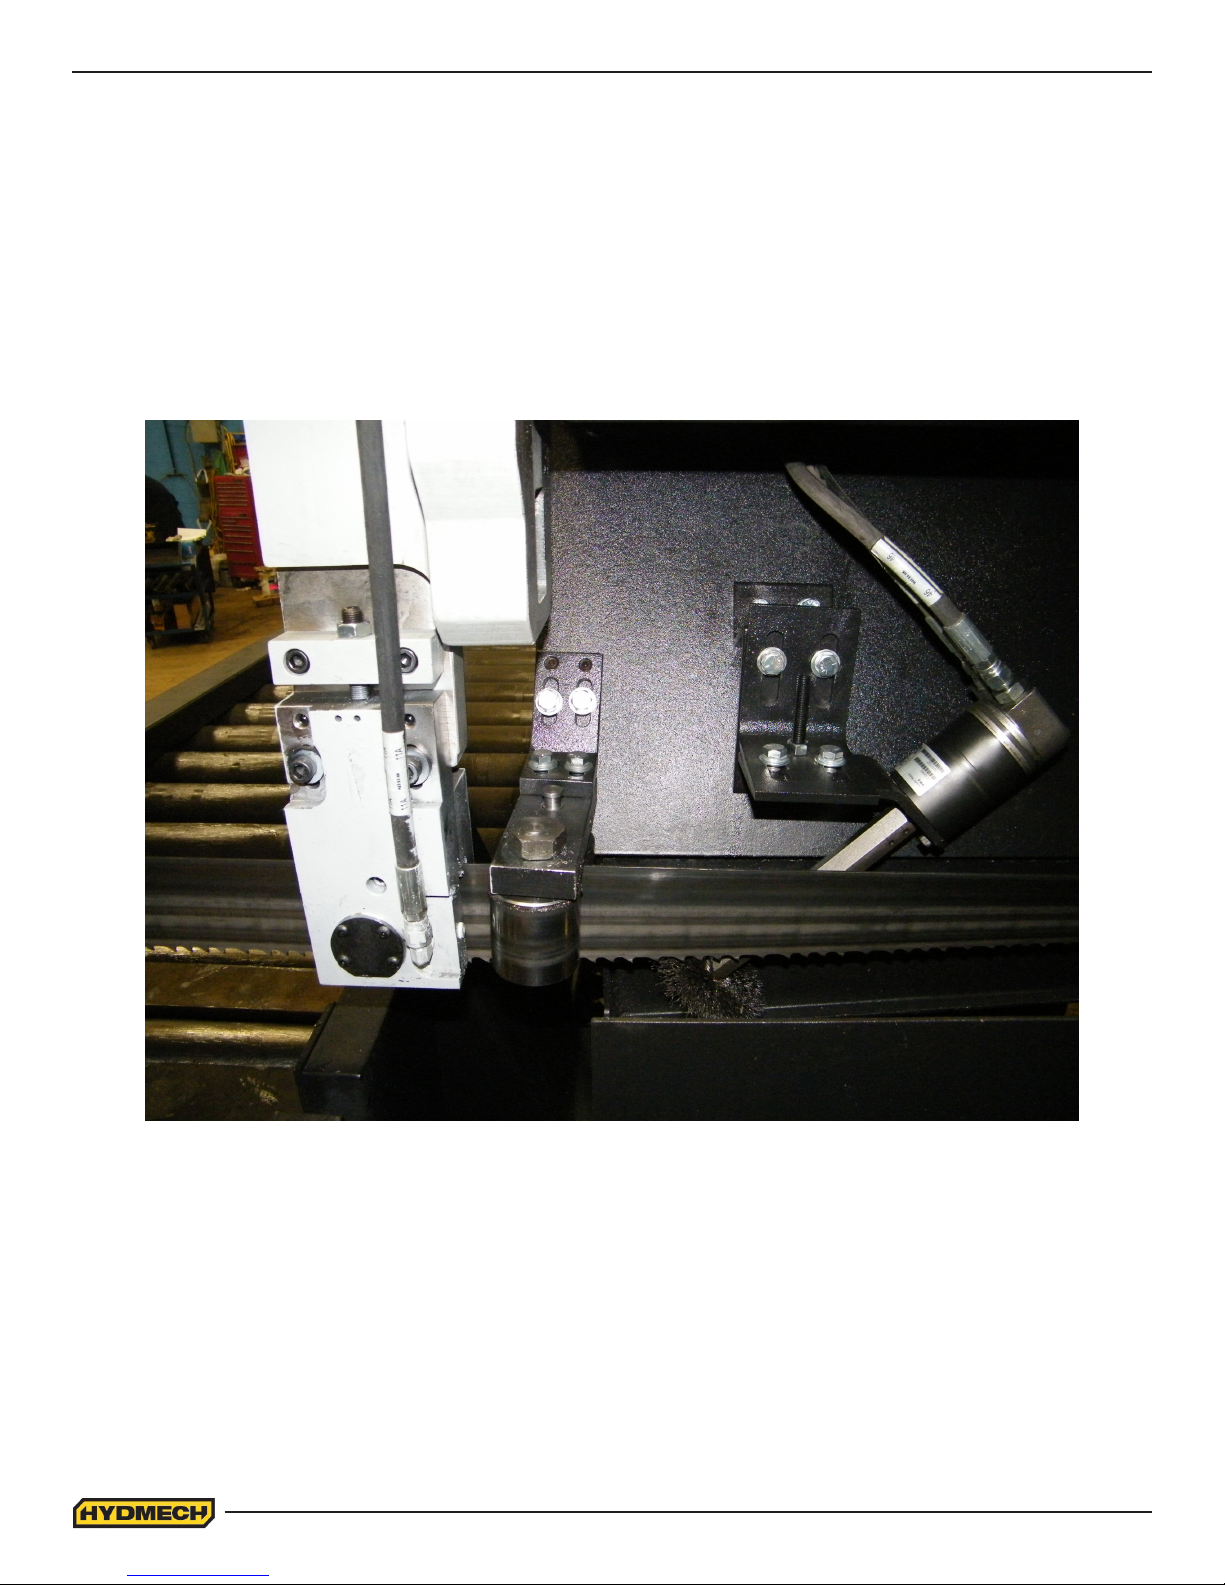
The blade brush is properly set when the machine leaves the factory, however, it wears out during operation and needs to
be adjusted periodically. The blade brush assembly is shown in the photo. In order to adjust it, the nut on the adjusting bolt
needs to be loosened and the brush mounting bracket turned until the wires from the brush touch the bottom of the blade
gullets as shown and then tighten the adjusting nut.
If the brush gets worn to approximately 70% of its original diameter, it should be replaced. A brush may be purchased
through a Hyd-Mech Group Limited dealer in your area.
3.4
Page 37
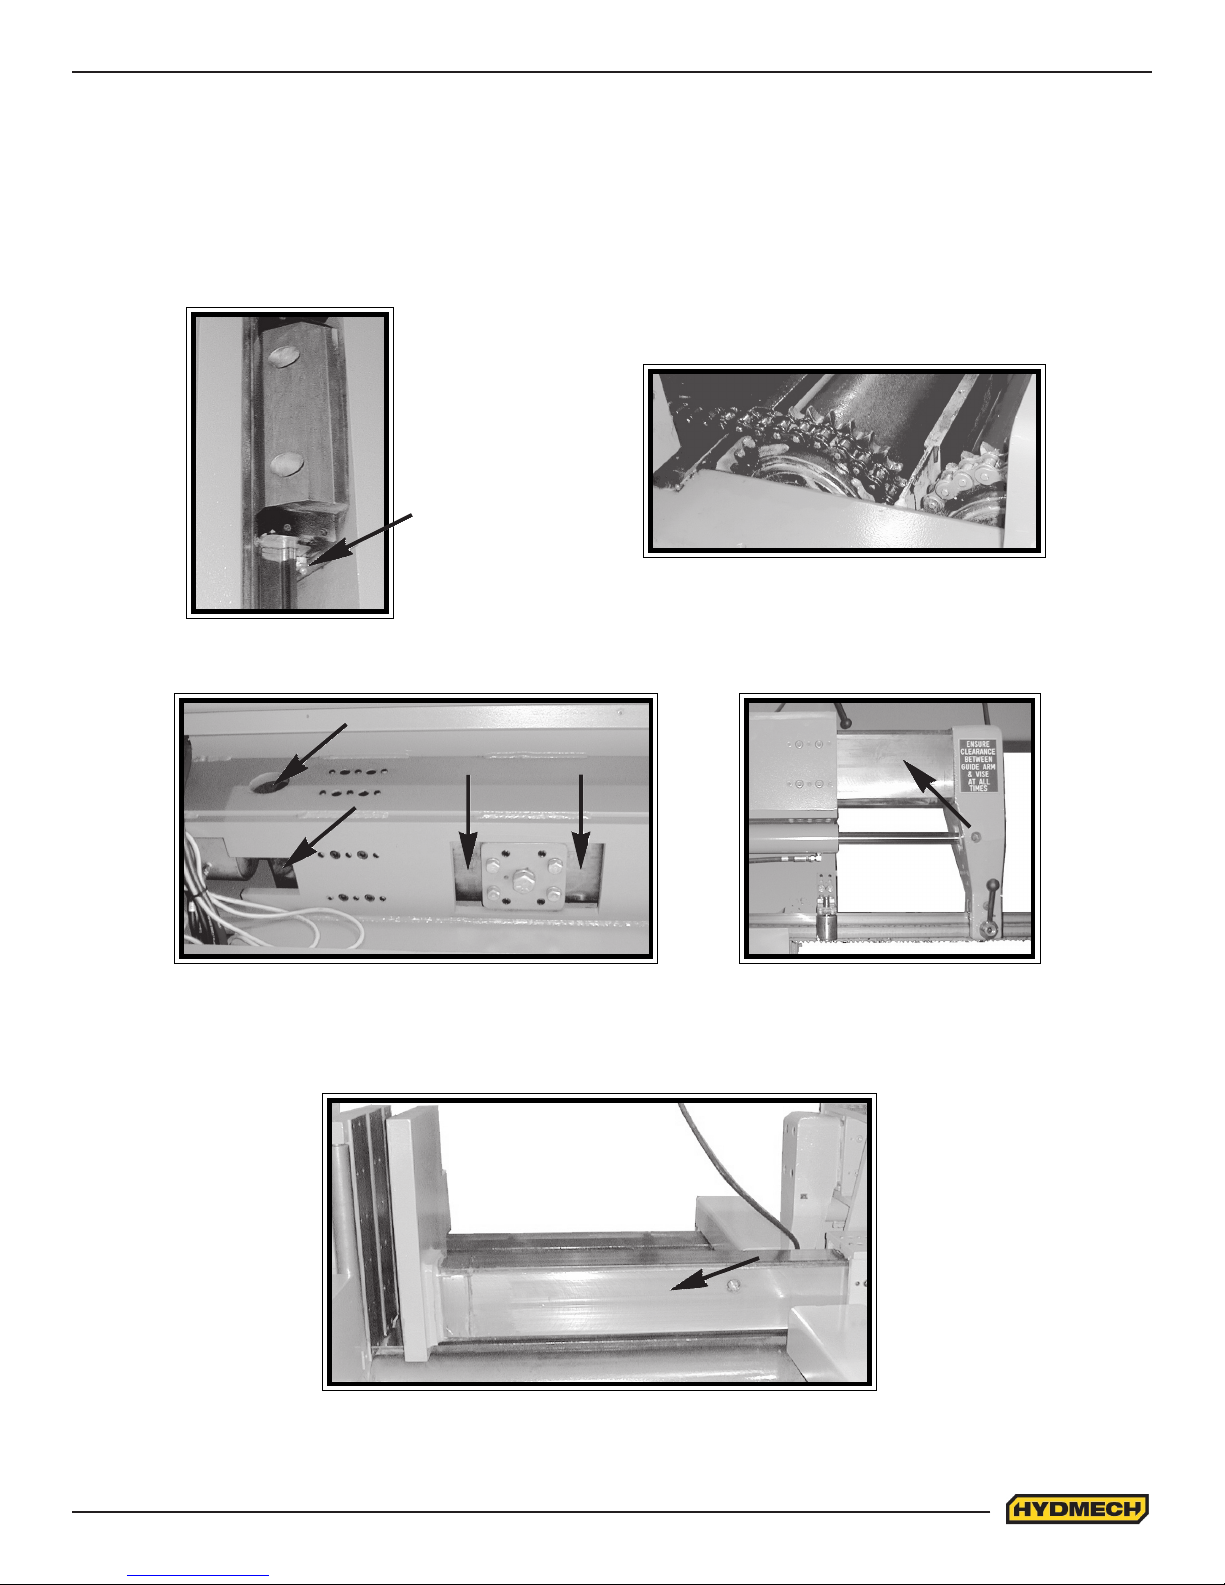
LUBRICATION
The design of the H-40 were intended to minimize maintenance, although periodically certain moving parts
need lubrication. We recommend that this periodic lubrication be done once a month using any general purpose
grease. In addition to the grease points shown, vise jaw guides and infeed rollers require greasing.
HYD-MECH recomends monthly lubrication.
LUBRICATION
The design of the H-40 was intended to minimize maintenance, although periodically certain moving parts need
lubrication. We recommend that this periodic lubrication be done once a month using any general-purpose grease. In
addition to the grease points shown, vise jaw guides and infeed rollers require greasing.
Hyd-Mech Group Limited recommends monthly lubrication.
Four linear bearings
with a grease nipple.
Roller chains.
Apply grease to the four places indicated on the
blade tension assembly.
(Shown with the cover removed.)
With the vis(s) closed, apply grease to all four sides of
Apply grease to all four sides
of the guide arm shaft with it
fully extended.
the vise shaft.
3.5
Page 38
HYDRAULIC MAINTENANCE
There are only FIVE items of routine maintenance associated with the hydraulic system:
1. OIL FILTER – Ten-micron ltration of the hydraulic oil is provided by a spin-on type lter mounted on the tank return
line. The element should be changed after the rst 50 Hours of operation and then every 500 working hours. Suitable
replacement elements are:
CANFLO RSE-30-10
GRESEN K-22001
PARKER 921999
ZINGA AE-10
2. OIL LEVEL - The oil level should be maintained in the upper half of the level gauge. Normally the rate of oil
consumption will be very low and it should be unnecessary to add oil more often than at lter changes. Add oil only to the
top line on the gauge. Hydraulic tank capacity is approximately 17 US gallons.
The machine is shipped from the factory with Texaco Rando HD 46 hydraulic oil. Generally any brand of recognized
mineral hydraulic oil with the same properties should be compatible with Texaco Rando HD 46 oil, but to avoid any risk we
suggest staying with Texaco Rando HD 46. If it is desirable to change brands, it is necessary to drain the tank and to ll to
1/3 with the new oil. Operate through several full strokes of each cylinder, drain the tank again, and nally ll the tank with
the new brand.
Recommended replacement oils: Chevron AW Hydraulic Oil 46
ESSO NUTO H46
Mobil Mobil DTE 25
Shell Tellus 46
Petro Canada Harmony AW 46
3. OIL TEMPERATURE – Oil temperature is indicated by a thermometer contained in the level gauge. Oil temperature
during steady operation should stabilize at about 50-55°F (10-12° C) above room temperature. Thus in a 70° F (20° C)
shop one might expect an oil temperature of about 120° F (50°C) Oil temperature should never exceed 160°F (70°C).
4. OIL PRESSURE – Oil pressure is factory set to 1500 PSI (10339 kPa) for H-40 and should not require further attention
except precautionary observation at start-up and every few days thereafter.
CLEANLINESS
The H-40 series design should endure heavy operating conditions and provide the customer with awless machine
performance. To extend good performance some care is required, especially cleanliness. The following areas should be
kept clean of dirt, grease and chips:
CONTROL CONSOLE
DOOR CHARTS
WHEEL BOXES
BLADE GUIDES
NOTE: All parts should be cleaned before any repair or service is performed on them.
3.6
Page 39
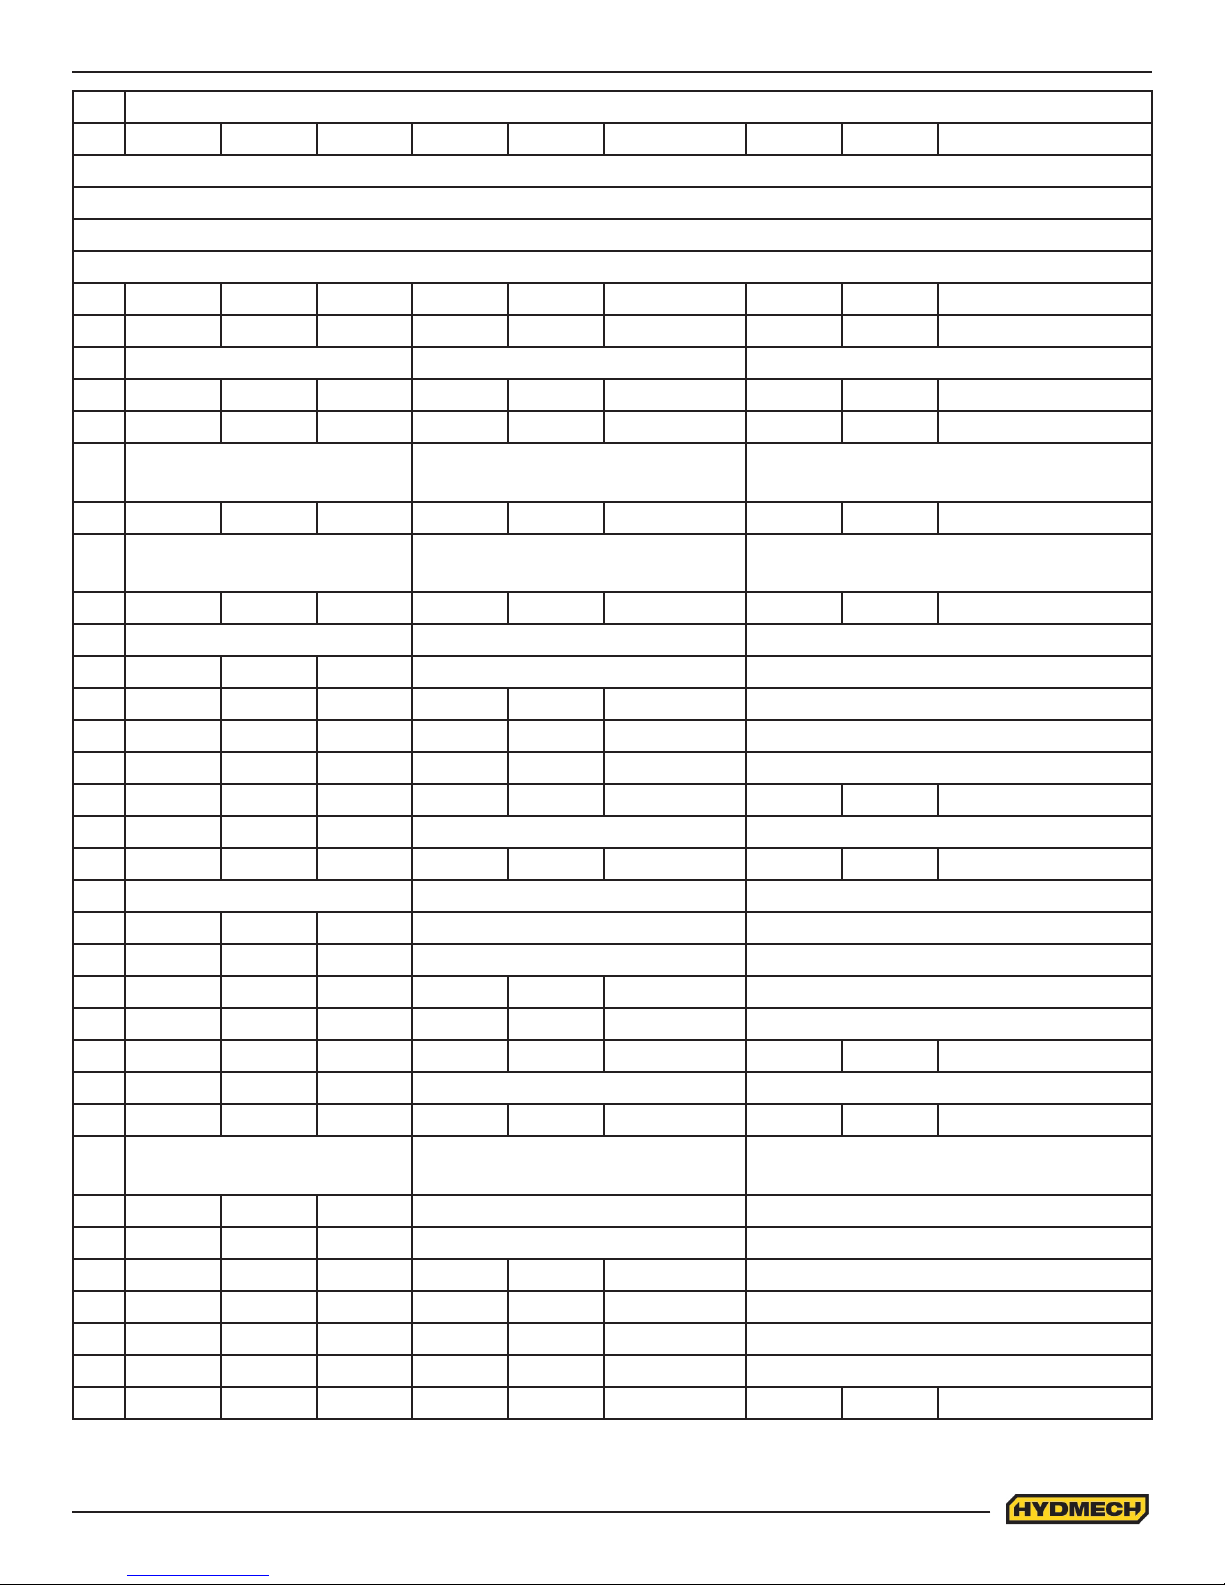
TROUBLE SHOOTING GUIDE
Most problems which may occur have relatively simple solutions which appear in this
section. If the solution is not found here, contact the Hyd-Mech Distributor from whom
you purchased your bandsaw. They have trained eld service personnel who will be able
to rectify the problem.
PROBLEM PROBABLE CAUSE SOLUTION
1 Saw is cutting out of
1. Blade worn. 1. Change blade.
square vertically
2 Saw is cutting out of
2. Stock not square in vises. 2. Adjust accordingly.
square horizontally
3 Blade comes o wheels. 3a. Not enough blade tension 3a.Blade tension is
determined by system
pressure. Check that
system pressure is as
specied above.
3b. Improper tracking. 3b. Set tracking.
4 Blade stalls in cut. 4a. Not enough blade tension 4a. Blade tension is
determined by system
pressure. Check that
system pressure is as
specied above.
5 Blade vibrates excessive-
ly.
4b. Excessive feed force. 4b. Reduce.
5a. Blade speed too fast. 5a. Reduce.
5b. Guide arms too far apart. 5b. Adjust accordingly.
5c. Not enough blade tension 5c. Blade tension is
determined by system
pressure. Check that system
pressure is as specied
above.
3.7
Page 40
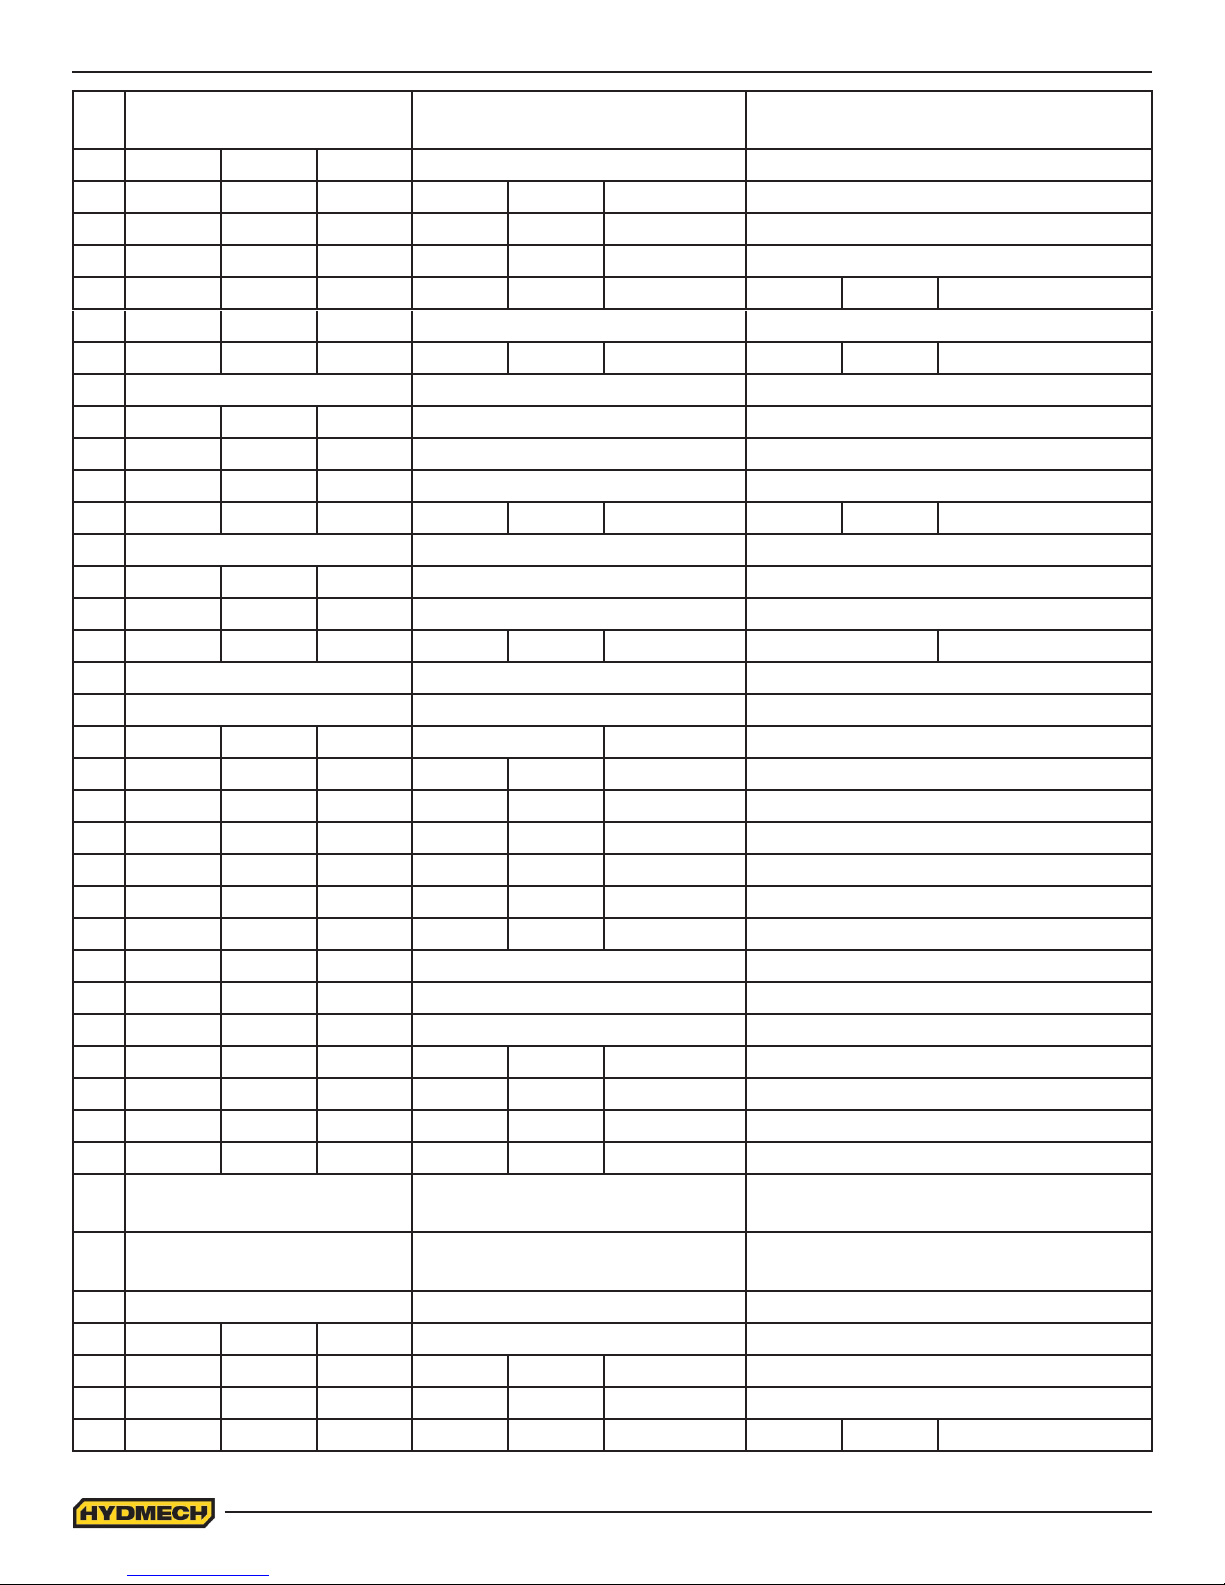
6 Excessive blade break-
6a. Excessive blade tension 6a.Blade tension is
age.
determined by system
pressure. Check that system
pressure is as specied
above.
6b. Excessive feed rate. 6b. Reduce.
7 Tooth Strippage 7a. Blade pitch too ne 7a.Select coarser pitch.
7b. Blade brush not cleaning 7b. Adjust or replace brush.
7c. Excessive feed rate 7c. Reduce
7d. Excessive feed force 7d. Reduce
8 No coolant ow 8a. No coolant. 8a. Add coolant.
8b. Coolant line blocked. 8b. Blow out coolant line.
8c.Coolant pump inoperable. 8c. Check, replace if
necessary.
9 Saw will not start. 9a.Motor overload has 9a. Depress each of the
tripped. overload buttons located
in the electrical box.
Depressing one button at a
time and trying to start the
saw will indicate which
motor was overloaded.
9b. Control circuit fuse has 9b. Replace the fuse with a
blown. 5 Amp 250 Volt AG1 type
fuse. Random blowouts
may occur but a quickly
repeated blow out indicates
an internal wiring fault
10 Saw starts but will not
10.On machines so 10. Reload with stock or
run
after Start button has
equipped, the out-of-stock re mount blade. Hold the
been
released. blade breakage limit switch hydraulic start button and
has been tripped. release the blade tension
or open vises far enough
to deactivate the limit switch.
3.8
Page 41
11 Saw starts but no hydrau-
11a. If blade wheels run 11a. Stop immediately;
lic
functions. clockwise, wrong phase reverse any two of the three
order in power connection phase connections.
to saw.
11b. If pump is noisy cause 11b. Stop immediately; add
may be low hydraulic oil level. hydraulic oil.
11c. Pump-motor coupling 11c. Adjust accordingly.
has separated.
12 Individual functions will
12a. Observe pilot light (s) on 12a. Solution usually requires
not
respond to its manual relevant valve. If pilot light opening the control console,
control switch. related to inoperative function and should be left to some
fails to light, problem is one qualied to work on
electrical. machine tool electrical
systems.
12b. If pilot light related to 12b. Solution usually requires
inoperative function does opening the control console,
light, problem may be the and should be left to some
coil. If problem remains after one qualied to work on
swapping coils it probably machine tool electrical
results from dirt in the valve systems.
spool.
13 Saw starts but only front 13a. Mode selector switch 13a. Select “manual” mode.
vise functions. is in “neutral”.
14 Head will not rise. 14a. Head up limit is set 14a. Readjust head up limit
fully down. switch bracket.
3.9
Page 42
15 Head still will not rise or
15a. Observe pilot light (s) 15a. In case of head function
fall,
or any individual function
on relevant valve. If pilot check operation of related
will
not respond to its manual light related to inoperative limit switches. Limit switch
control switch. function fails to light, problem levers should operate
is electrical. freely and emit an audible
click on both depress and
release. If not replace the
switch nose. Look for cause
of switch damage (ie debris
or maladjustment of switch
actuator). To check the
switch unit itself, remove the
switch lid and wire together
the two terminals closest
to the wiring port. If function
now responds to manual
switch replace internal
limit switch unit. If function
still does not respond then…
Open panel door to gain
access to valves. Remove
coil retaining nut and
withdraw problem related
coil, replace it with any
other coil from the group.
If the problem remains it
requires the attention of a
qualied service person.
15b. If pilot light related to 15b. Disassembly of
inoperative function does hydraulic valves should be
light, problem may still be undertaken only by
the coil (see 15a. Solution). qualied service personnel
If problem remains it or those knowledgable with
probably results from dirt in hydraulic components.
the valve spool.
3.10
Page 43
16 Head will not descend. 16a. Feed Rate Valve is 16a. Turn Feed Rate Knob
fully closed-pointer is set on counter clockwise to open
“0” or close to “0” in/min. valve.
16b. Feed Force Limit is set 16b. Increase Feed Force
too low. Limit (to at least 150 psi).
16c. Pointer is not adjusted. 16c. Loosen printer, turn
knob clockwise until it
bottoms; tighten pointer at
“0”.
17 Head descends when
17a. Pointer of Feed Rate 17a. Re-adjust pointer. As in
Feed
Rate Valve pointer is set tovalve is stopped by stop 16c.
“0” on the scale and Feed bolt but not fully closing the
Force Limit gauge is
valve.
more
than 150 psi.
3.11
Page 44
SECTION 4 - ELECTRICAL
ELECTRICAL SCHEMATICS: SEE PDF ON ATTACHED CD
4.1
Page 45
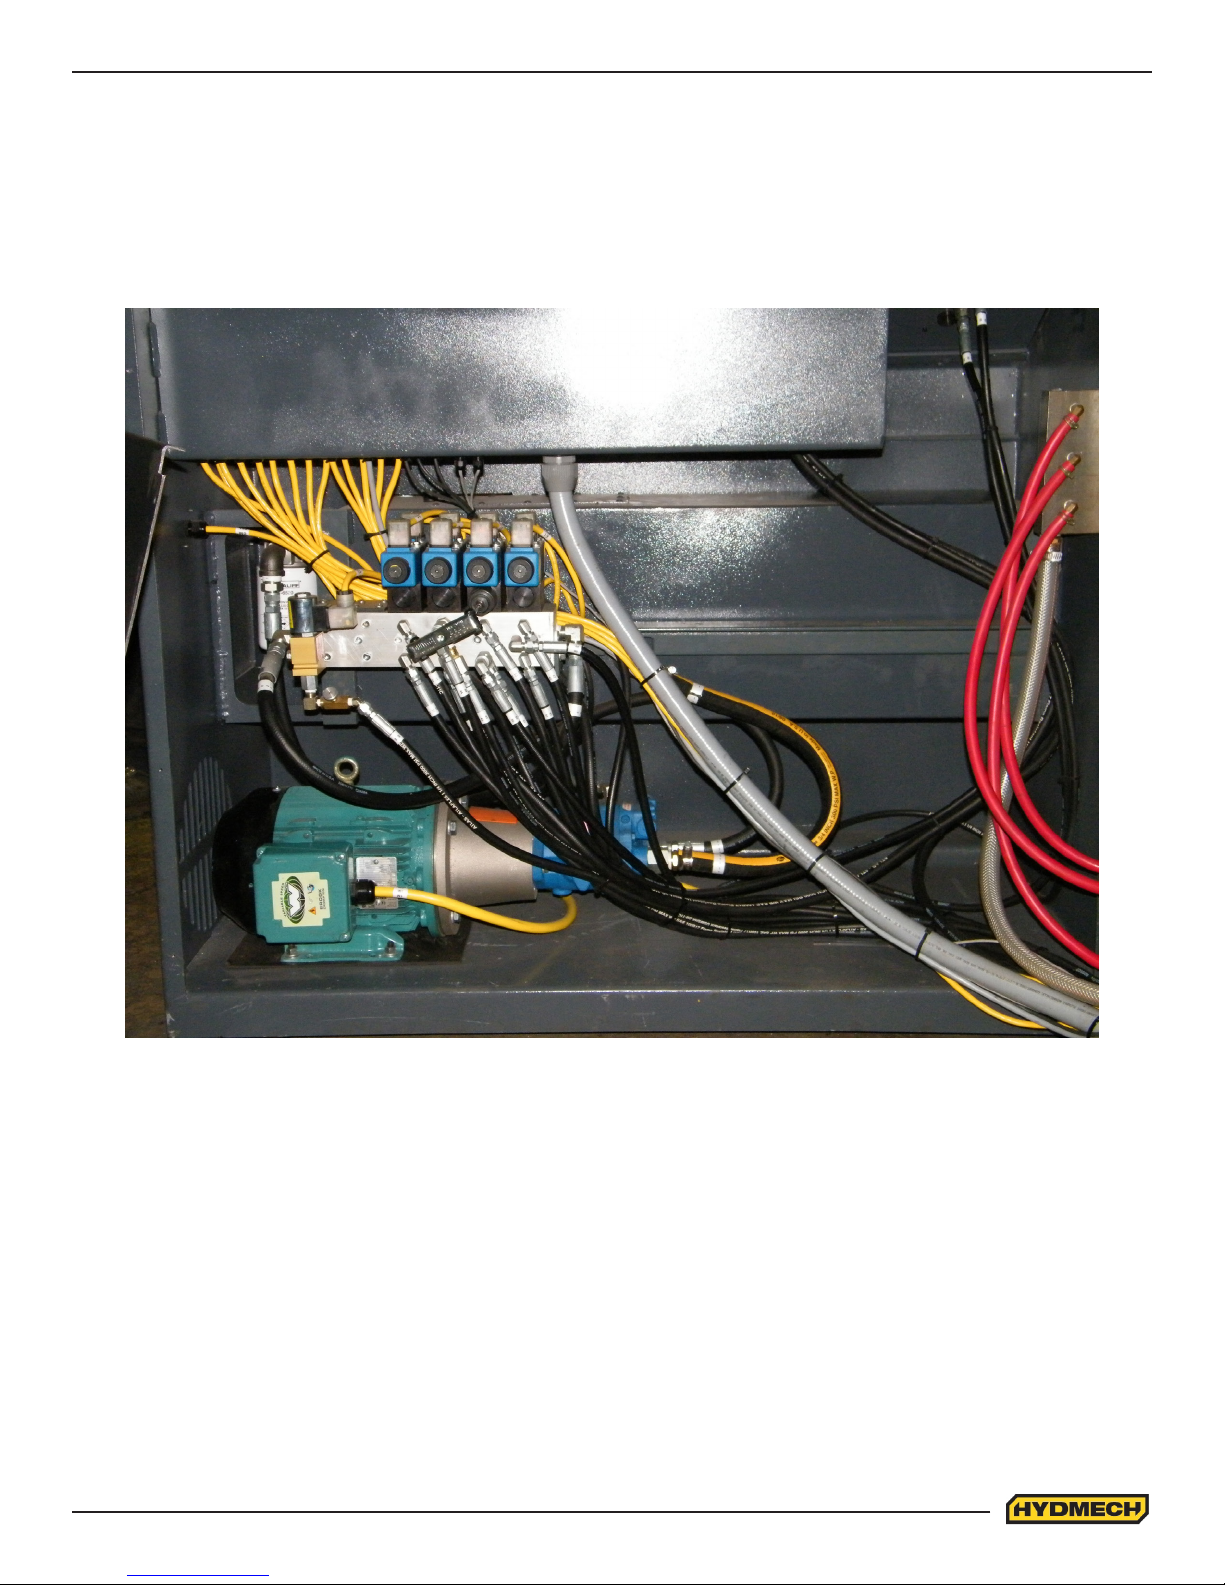
SECTION 5 - HYDRAULIC SYSTEM
The H-40 hydraulic system does not require any special work on a new machine before its start-up. The
hydraulic tank is lled with Texaco Rando 46 hydraulic oil and all machine functions have been tested at the
factory to ensure proper operation upon initial start-up.
HYDRAULIC MANIFOLD AND MOTOR ASSEMBLY
5.1
Page 46
LIST OF H-40 HYDRAULIC COMPONENTS
ITEM QUANTITY DESCRIPTION PART NUMBER
1 2 HEAD CYLINDER H40-C4-00B
2 1(2) VISE CYLINDER V18A-C1-00A
3 1 BLADE TENSION CYLINDER H40-C5-00A
4 1 GUIDE ARM POSITIONING CYLINDER H40-C6-00
5 1 MANIFOLD BLOCK MB1 MB6P
6 3(4) DOUBLE PILOT CHECK DPCH-1
7 2 PRESSURE GAUGE (1000 PSI) PG-10
8 1 PRESSURE GAUGE (2000 PSI) PG-15
9 1 CHIP CONVEYOR DRIVE MOTOR HM-01 (MG12)
10 1 BRUSH MOTOR HM-02
11 0(1) REAR VISE VALVE DCV3P-AB-T
12 1 FRONT VISE VALVE DCV3P-AB-T
13 1 HEAD VALVE DCV3P-AB-T
14 1 BLADE TENSION VALVE DCV3P-AB-C
15 1 PRESSURE REDUCING VALVE PRV-2
16 1 GUIDE ARM VALVE DCV3P-AB-T
17 1 SINGLE SOLENOID TWO WAY VALVE PV2P-A-C
18 1 RELIEF VALVE RV7
19 1 FEED RATE VALVE DF7-0-00
20 1 PUMP HYP-1
21 1 SUCTION STRAINER TFS-100-0-P
22 1 RETURN FILTER SF6520
23 1 COOLER AO-10
24 2 NEEDLE VALVE N10BK
25 1 CHECK VALVE CHV
HYDRAULIC SCHEMATICS & PLUMBING DIAGRAMS: SEE PDF
ON ATTACHED CD
5.2
Page 47
SECTION 6 - MECHANICAL ASSEMBLIES
MECHANICAL ASSEMBLY DRAWINGS & PARTS LIST: SEE PDF
ON ATTACHED CD
6.1
Page 48
SECTION 7 - OPTIONS
BLADE DEVIATION MONITORING SYSTEM (K10)
OPTIONAL ASSEMBLY DRAWINGS: SEE PDF ON ATTACHED CD
BLADE DEVIATION MONITORING SYSTEM (K10)
General description of the blade deviation monitoring system.
This system monitors lateral blade deviation during cutting. If blade deflection increases beyond
the pre-set warning limit, then the monitoring device sends a warning signal by means of
flashing beacon mounted on the top of machine head. If no steps are taken to correct this
condition, the machine will continue to cut until the pre-set shut-down limit is reached. At this
point the machine will behave in one of two ways, selectable by parameter setting:
1. Stop cutting, raise the head and shut down
or
2. Finish the cut with present degree of deviation and then shut down.
Operation of the system
The proximity transducers are enclosed in a housing mounted on the idler and drive side guide
arms. The sensors convert the blade lateral deflection to an analog signal, which is sent to the
PLC and after a series of calculations is displayed on the operator interface in a form of bar
graphs. One bar graph for the transducer mounted on the idler guide arm and the second bar
graph for the transducer mounted on the drive side guide arm.
The bar graphs appears in both Manual Mode and Automatic Mode Screens. It is only active
when the blade is running and head is descending. The length of the bar graph is proportional to
the blade deflection. The bar graphs extend from the screen centre towards the right if blade is
deviating toward the front of the saw (cutting into the part), and extends from the screen centre
towards the left if blade is deviating toward the rear of the saw (cutting into the stock).
If a warning limit is reached and maintained longer than the preset response time, then the
beacon light mounted on the top of the head will start flashing.
If a shutdown limit is reached and maintained longer than the preset response time, then the
machine will behave in one of two ways: stop cutting, raise the head and shut down or finish the
cut with present degree of deviation and then shut down.
7.1
Page 49
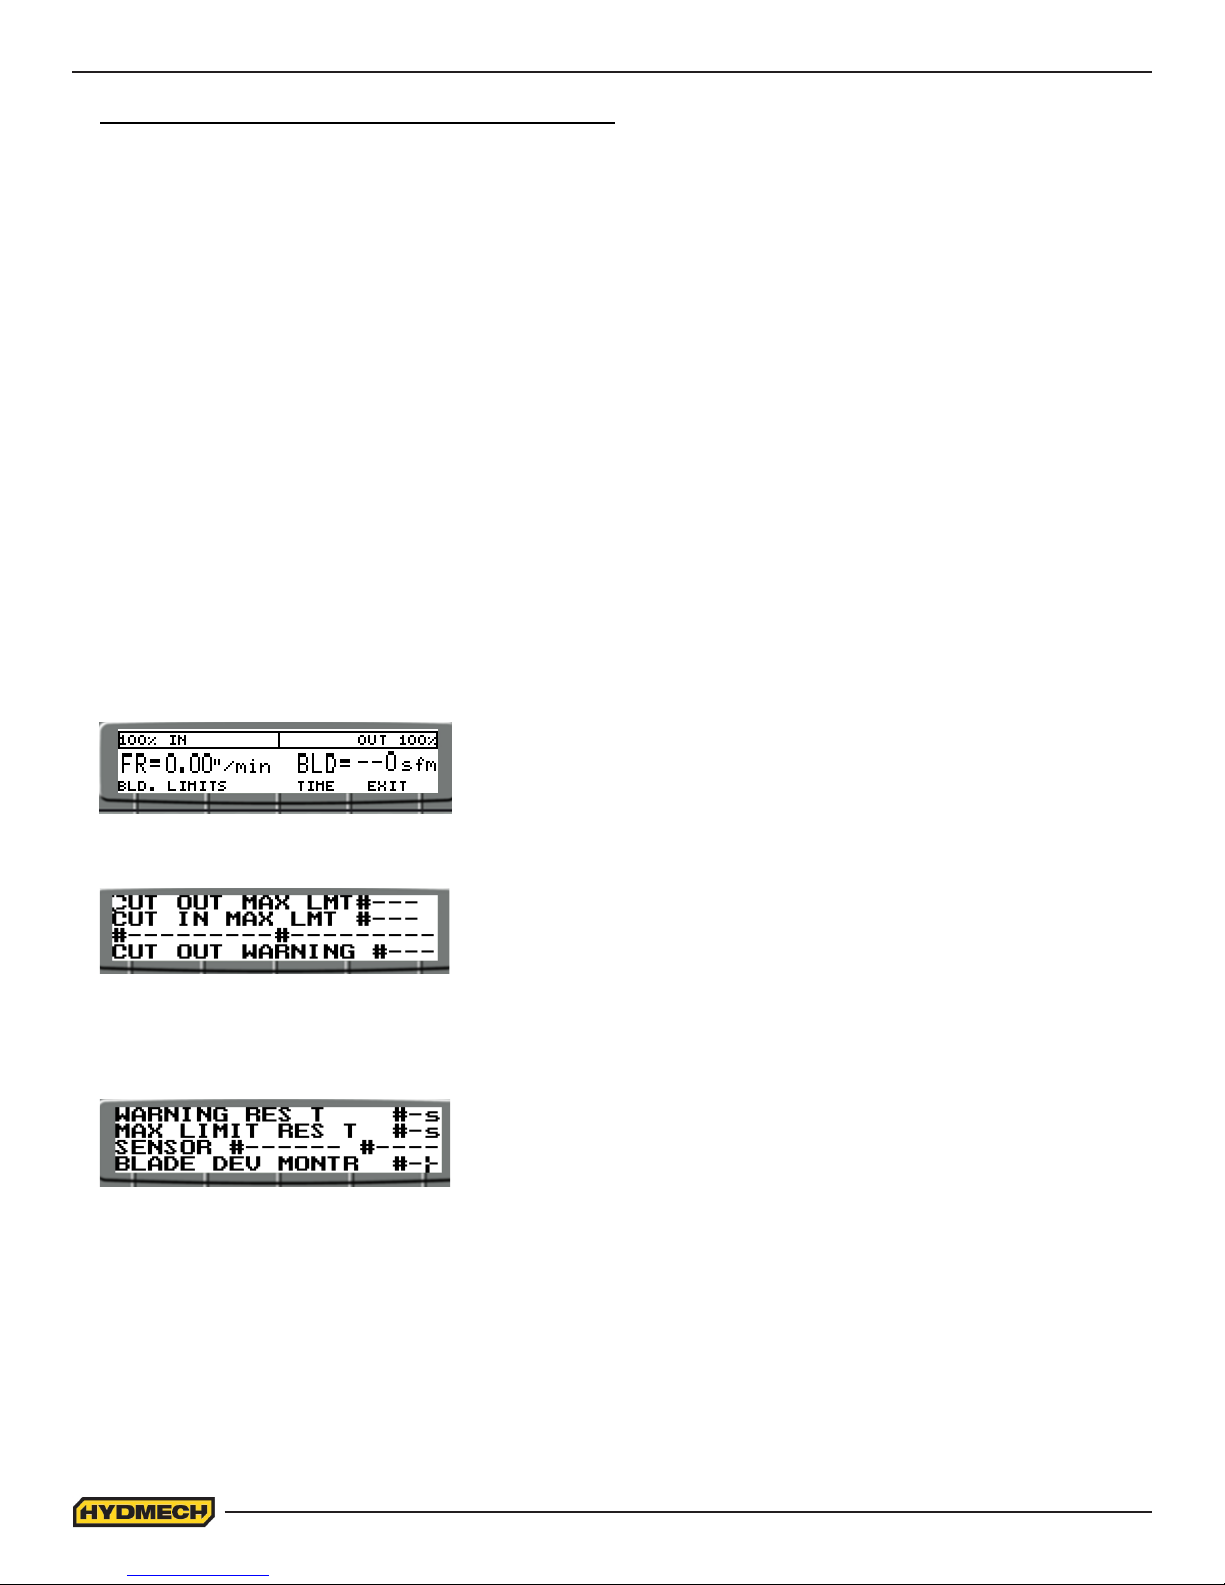
Procedure to access blade deviation parameters
- To adjust the warning and shutdown limits, enter MONITOR LIMIT SETTING screen
by pressing F2 (BLD. LIMITS) access blade deviation limit settings (Figure 1).
The MONITOR LIMIT SETTING screen will be displayed (Fig. 2)
- Enter parameters screen by pressing function key F3.(Labeled: PARMTR) The
PARAMETER SETTING screen will be displayed (Fig. 3).
- Change BLADE MONITOR parameter to ON by moving the cursor using the
navigation keys to ON/OFF and pressing ENTER. The value of Blade Monitor
parameter will change to ON.
- Exit parameter screen by pressing function key F5.
Repeating the above steps will disable the blade monitor option.
Warning and shutdown limits adjustments
To adjust the warning and shutdown limits, enter MONITOR LIMIT SETTING screen by pressing
Press F2 (BLD. LIMITS) to access blade deviation limit settings (Figure 1).
Fig1
Fig2
PressF3(PARMTR)toaccessparameters.
Fig3
Usecursorkeytoscrollthroughtheparameterslist.
PressF5toreturntopreviousscreen
7.2
Page 50
The MONITOR LIMIT SETTING screen will be displayed Figure 2.
There are two scales, the upper one showing the preset right and left shutdown limits, and the
lower scale showing the preset right and left warning limits. All four limits (right and left warning
and right and left shutdown) are set independently.
To adjust limits move cursor to number on right hand side of the screen and key in new value
from – 100 to 0 for cut out limit and from 0 to 100 for cut in limit.
CUT OUT MAX LIMT 50
CUT IN MAX LIMT -50
_ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _
CUT OUT WARNING 30
CUT IN WARNING -30
_ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _ _
Figure 2 Monitor Limit setting screen.
Cut out maximum limit – (out - cutting towards outfeed, range 0 ~100). This parameter will
adjust shutdown limit if blade is cutting towards the part. Increasing this value decreases
sensitivity, which will result in a larger deviation from nominal straight, before shutdown
sequence is initialized.
Cut in maximum limit – (in - cutting towards infeed, range -100 ~ 0) This parameter will adjust
shutdown limit if blade is cutting towards the stock. Decreasing this value decreases sensitivity,
which will result in a larger deviation from nominal straight, before shutdown sequence is
initialized.
Cut out warning limit – (out - cutting towards outfeed, range 0 ~100) This parameter will
adjust warning limit if blade is cutting towards the part. Increasing this value decreases
sensitivity, which will result in a warning further from nominal straight.
Cut in warning limit – (in - cutting towards infeed, range -100 ~ 0) This parameter will adjust
warning limit if blade is cutting towards the stock. Decreasing this value decreases sensitivity,
which will result in a warning further from nominal straight.
7.3
Page 51
To return from the MONITOR LIMIT SETTING screen to Auto or Manual screens, press EXIT
F5 function key
To access the parameters screen (Figure 3), press PARMTR (F3) function key.
WARNING RESPONSE TIME
MAX LIMIT RESPONSE TIME
SENSOR
BLADE DEVIATION MONITOR
DISPLAY REFRESH RATE
Xs
Xs
XXXX
ON
2/s
Figure 3 Parameter screen.
To set any of the numerical parameters, use the NAVIGATION keys (Figure 1) to place the
cursor over the number. Key in the desired value, and then press ENTER.
To change the ON/OFF parameters, place the cursor over the parameter, and press ENTER to
toggle between ON and OFF.
Warning response time (range 2 – 99 seconds)
WARNING RESPONSE TIME
MAX LIMIT RESPONSE TIME
If the blade deviation exceeds the preset warning limit for longer than warning
response time, then the beacon light mounted on the top of the head will start
flashing.
Maximum limit response time – (range 2 – 99 seconds)
If the blade deviation exceeds the preset shutdown limit for longer than
shutdown response time, then the machine will execute shutdown sequence.
(range –2000 – +2000)
The number displayed here represents the position of the blade within the
SENSOR
BLADE DEVIATION MONITOR ON/OFF
DISPLAY REFRESH RATE
measuring range of the proximity transducer. At 0, the blade is exactly
centered within the sensing range. The display assists adjustment with the
prompts ‘SETTING, or ‘SET’. The prompt ‘SET’ appears when the adjustment
is within the acceptable range of – 100 +100.
[See sensor adjustment procedure section]
This parameter will activate or deactivate response of the blade deviation
monitoring system.
(range 0.1 sec – 10 sec)
The refresh time is time between bar graph updates. If it is set to low value
then the display will flicker do to vibration of the blade, weld passing by the
sensor or other irregularities in the blade.
Figure 4 Parameter description chart.
Relationship between Blade Deflection Display and Actual Cut Deviation
The digital display indicates the blade lateral deflection at the point where it passes the blade
deflection sensor, which is 1” past the idler side guide arm. The display range of0 +/-100 is
proportional to the amount of blade deviation. This depends on the type of material, shape of
the work-piece and amount of blade tension. The maximum deviation of the cut surface will
occur at or near the center of the cut, and will be several times larger than that measured at the
sensor.
The actual amount is difficult to predict, experience with different work-pieces will
provide the best guide.
7.4
Page 52
SECTION 8 - SPECIFICATIONS
H4040 SPECIFICATIONS
H-40-40 BANDSAW SPECIFICATIONS
Capacity
Blade
Blade Tension
Blade Speed VFD 45 - 225 sf/min (14 - 68 m/min)
Blade Guides
Blade Wheel Dia.
Motors
Pumps
Hydraulic Tank
Coolant Tank
System Pressure
Vise Control
round 41" (1042mm)
rectangular 41"x 41"(1042mm x 1042mm)
Length 37'-0" (11278mm)
Width 3" or 2 5/8" (76mm or 67mm)
thickness .063" (1.6mm)
Hydraulic
carbide inserts
45" (1143mm)
blade drive 20 HP (15 KW)
hydraulic pump drive 5 HP (3.7 KW)
Hydraulic 6 1/2 U.S. Gal. / min (25 Liters/min) pressure compensated
Coolant 16.6 U.S. Gal. / min (63 Liters/min)
17 U.S. Gallons (64.5 Liters)
27 U.S. Gallons (102.5 Liters)
1200 PSI (8274 kPa)
hydraulic
Table Height
Control Panel
Machine Weight 39,000 lbs (19051 Kg)
Maximum Workload
Overall Dimensions
27" (686mm)
Waist Height
42,000 lbs (20412 Kg) with optional outboard vise
42000 lbs (19051 Kg)
221" (5613mm) Wide, 119" (3023mm) Long, 148" (3759mm) High
8.1
Page 53
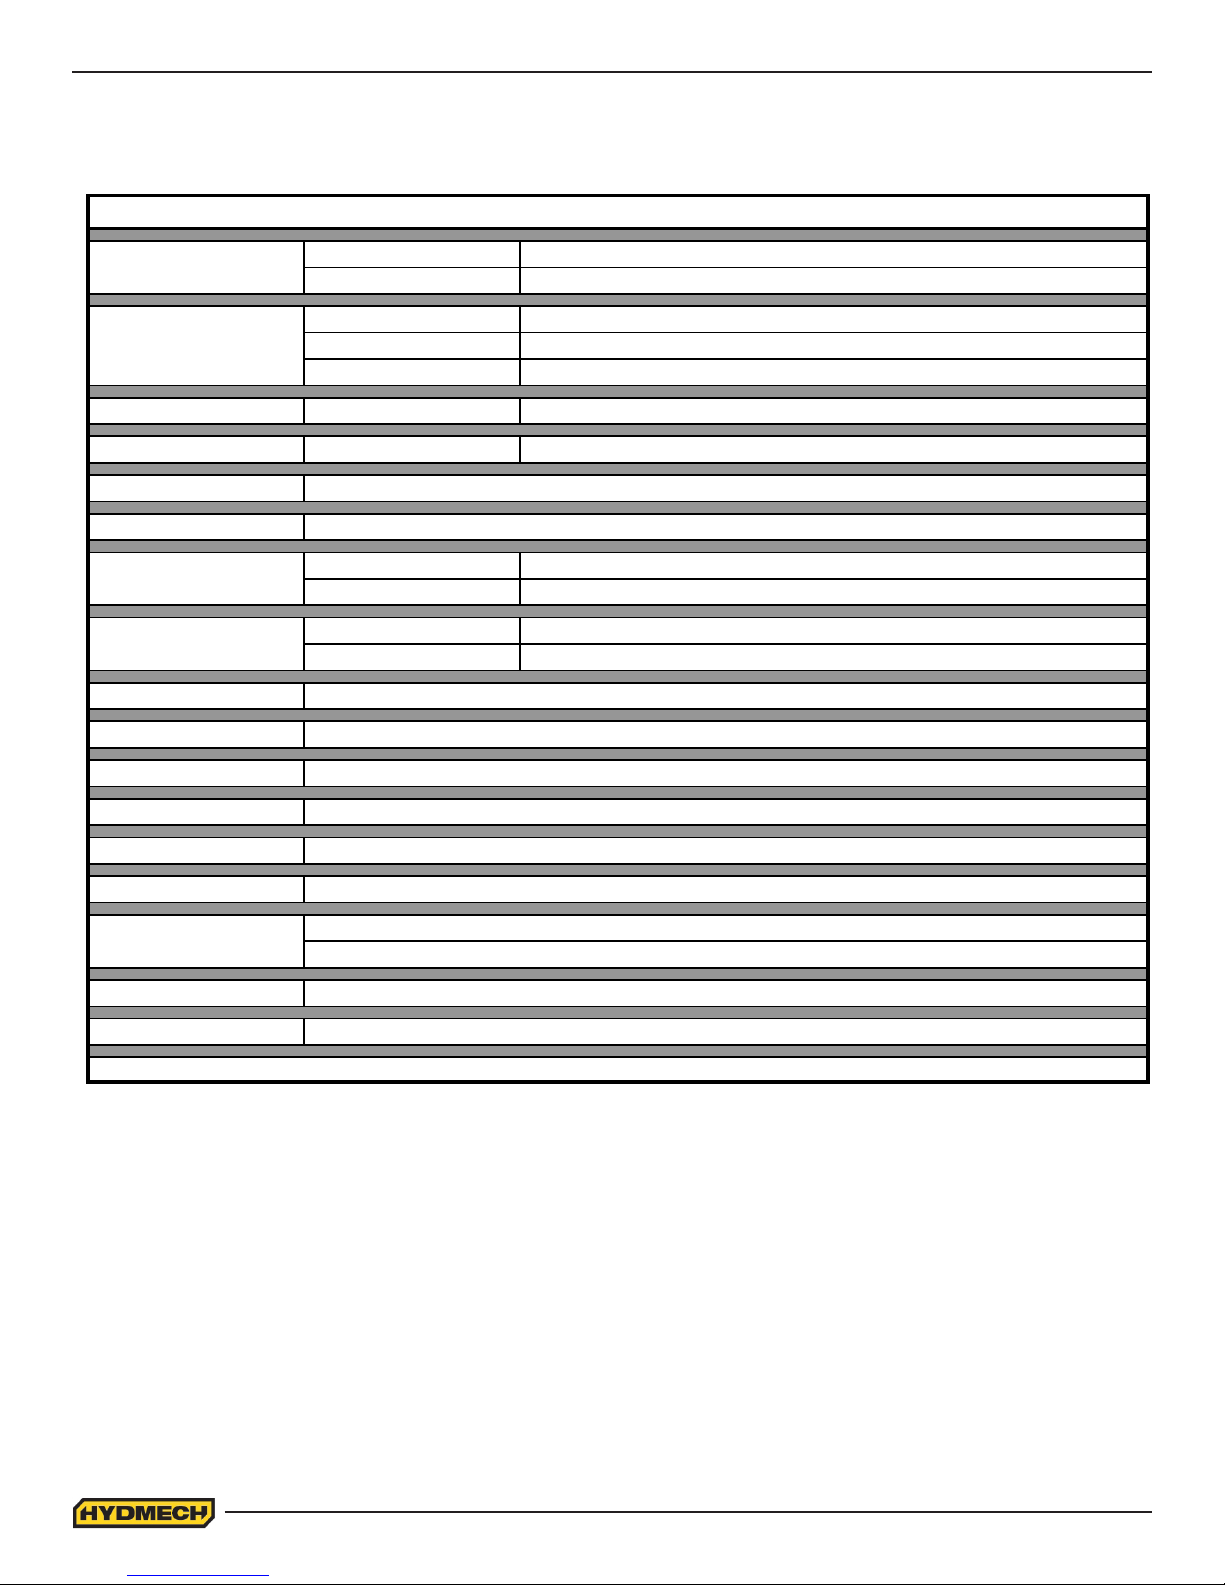
H4060 SPECIFICATIONS
H-40-60 BANDSAW SPECIFICATIONS
Capacity
Blade
Blade Tension Hydraulic
Blade Speed VFD 45 - 225 sf/min (14 - 68 m/min)
Blade Guides
Blade Wheel Dia.
Motors
Pumps
Hydraulic Tank
Coolant Tank
System Pressure
Vise Control
round 41" (1042mm)
rectangular 41"x 61"(1042mm x 1550mm)
Length 40'-4" (12294mm)
Width 3" or 2 5/8" (76mm or 67mm)
thickness .063" (1.6mm)
carbide inserts
45" (1143mm)
blade drive 20 HP (15 KW)
hydraulic pump drive 5 HP (3.7 KW)
Hydraulic 6 1/2 U.S. Gal. / min (25 Liters/min) pressure compensated
Coolant 16.6 U.S. Gal. / min (63 Liters/min)
17 U.S. Gallons (64.5 Liters)
27 U.S. Gallons (102.5 Liters)
1200 PSI (8274 kPa)
hydraulic
Table Height
Control Panel
Machine Weight 42,000 lbs (19051 Kg)
Maximum Workload
Overall Dimensions
27" (686mm)
Waist Height
45,000 lbs (20412 Kg) with optional outboard vise
50000 lbs (22680 Kg)
241" (6121mm) Wide, 119" (3023mm) Long, 148" (3759mm) High
8.2
Page 54
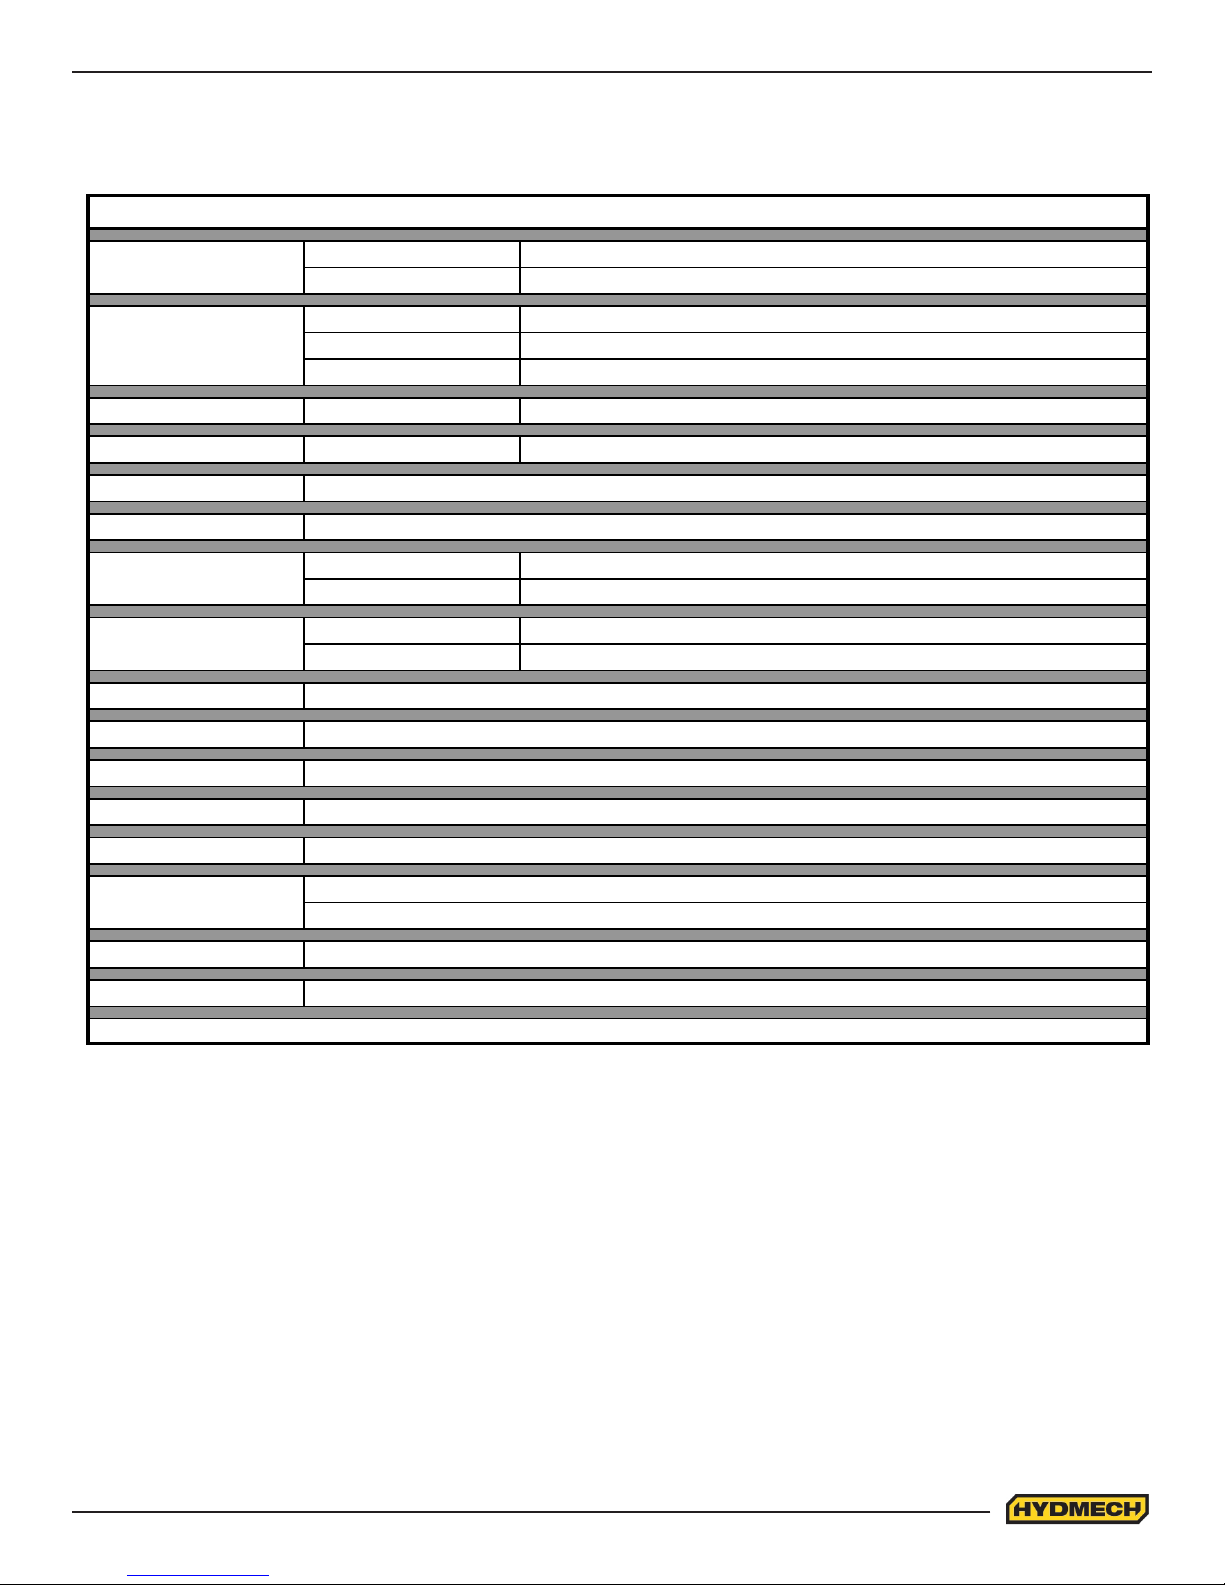
H4080 SPECIFICATIONS
H-40-80 BANDSAW SPECIFICATIONS
Capacity
Blade
Blade Tension Hydraulic
Blade Speed VFD 45 - 225 sf/min (13.5 - 67.5 m/min)
Blade Guides
Blade Wheel Dia.
Motors
Pumps
Hydraulic Tank
System Pressure
Vise Control
Table Height
round 41" (1042mm)
rectangular 41"x 81"(1042mm x 2058mm)
Length 43'-10" (13361mm)
Width 3" or 2 5/8" (76mm or 67mm)
thickness .063" (1.6mm)
carbide inserts
45" (1143mm)
blade drive 20 HP (15 KW)
hydraulic pump drive 5 HP (3.7 KW)
Hydraulic 6 1/2 U.S. Gal. / min (25 Liters/min) pressure compensated
Coolant 16.6 U.S. Gal. / min (63 Liters/min)
17 U.S. Gallons (64.5 Liters)
1300 PSI (8963 kPa)
hydraulic
27" (686mm)
Control Panel
Machine Weight 46,000 lbs (20865 Kg)
Maximum Workload
Overall Dimensions
Waist Height
50,000 lbs (22680 Kg) with optional outboard vise
50000 lbs (22680 Kg)
261" (6629mm) Wide, 119" (3023mm) Long, 148" (3759mm) High
8.3
Page 55
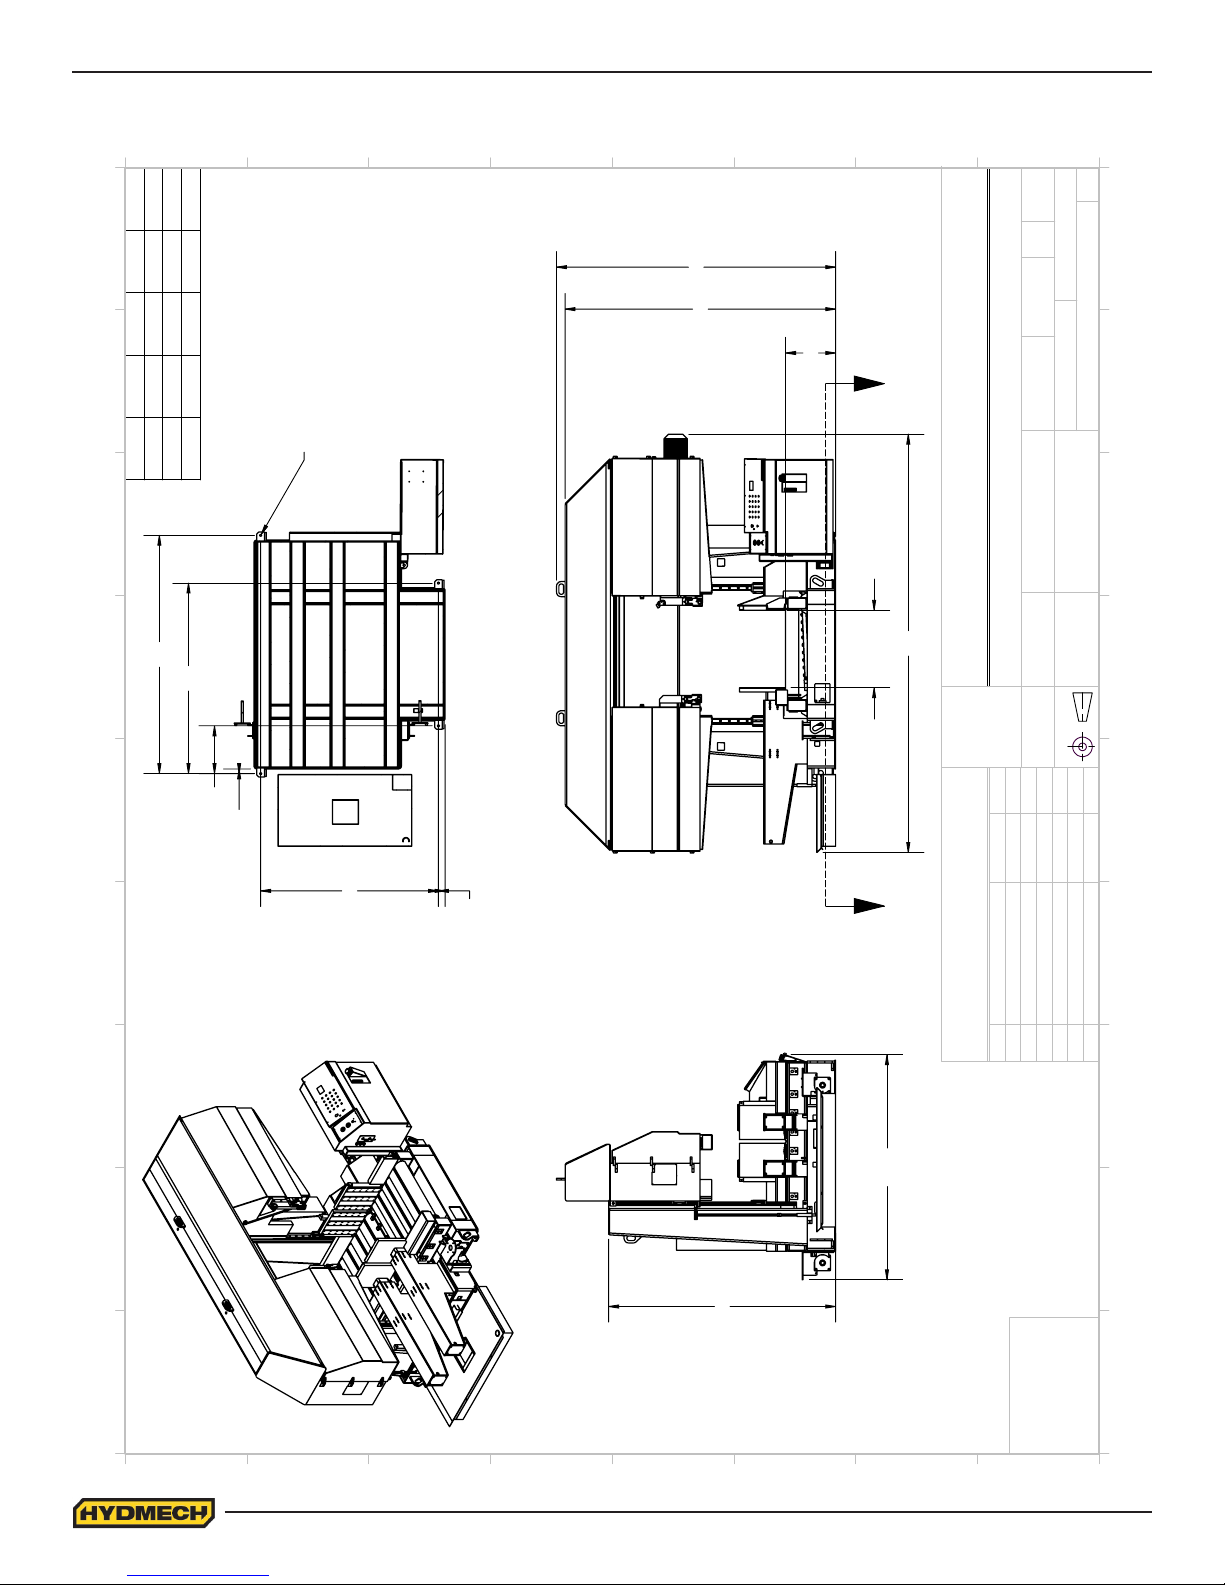
LAYOUT DRAWING
THE DATA/DESIGN CONTAINED HEREIN IS PROPRIETARY
AND CONFIDENTIAL.REPRODUCTION,PUBLICATION OR
DISTRIBUTION OF ANY PART REQUIRES WRITTEN CONSENT
OF HYD-MECH GROUP.THIS DATA IS THE PROPERTY OF
HYD MECH GROUP AND ITS POSSESION CONFERS NO
LICENSE TO USE OR RIGHT OR LICENSE TO DISCLOSE IT
TO OTHERS FOR ANY PURPOSE WHATSOEVER.
ALL RIGHTS RESERVED.
8
J
126"
146"
100.75"
120.75"
I
221"
241"
A B C D
41"
61"
H
H4040
H4060
166"
140.75"
261"
81"
H4080
7
6
1-8 UNC (x4)
5
4
3
148
143
27
2
1
SHEET
SCALE
CHKED BY:
1
OF
1
1:66
DATE:
COATING:
0
REV
-
No Coating
J
I
H40-0-00
AA
EngCoop
Jan 21, 2016
DRWN BY:
PART WEIGHT:
DRAWING NUMBER:
DATE:
WOODSTOCK. ONTARIO. CANADA N4S 0A9
H
HYDMECH GROUP LIMITED
MAT'L:
COMPONENT GROUP:
G
B
D
C
SECTION A-A
A
00 - Top Level
MODEL:
H4040
TITLE
H4040, H4060, H4080 MACHINE LAYOUT
G
MATERIAL CODE:
FOUNDATION PLAN
F
UNLESS
HYDMECH
STANDARD
TOLERANCES
SPECIFIED
OTHERWISE
DIMENSIONS
-
-
BY
ARE IN INCHES
THIRD ANGLE PROJECTION
F
25.25
2.5
E
DATE
-
-
E
94
3.5
REVISIONS
-
-
ECN NUMBER
D
C
B
120
119
REV
-
-
D
C
B
A
8
7
6
5
4
3
2
1
A
0
8.4
Page 56
SECTION 9 - WARRANTY
WARRANTY
Hyd-Mech Group Limited warrants parts/components on each new bandsaw to be free from failure resulting
from defective material and workmanship under proper use and service for a period of two years on following
the date of shipment from the factory. Hyd·Mech’s sole obligation under this warranty is limited to the repair or
replacement without charge, at Hyd·Mech’s factory, warehouse, or approved repair shop any part or parts which
Hyd·Mech’s inspection shall disclose to be defective. Return freight must be prepaid by the user.
This warranty, in its entirety, does not cover maintenance items, including but not limited to lubricating grease and oils,
lters, V-belts, saw blades, etc., nor any items therein which show signs of neglect, overloading, abuse, accident,
inadequate maintenance, or unauthorized altering.
MOTOR, GEARBOX, PUMP, ELECTRIC COMPONENTS, VALVES, HOSES, FITTINGS, and any other items used in the
manufacture of the saw, but not originally manufactured by Hyd·Mech are subject to the original manufacturer’s warranty.
Hyd·Mech will provide such assistance and information as is necessary and available to facilitate the user’s claim to such
other manufacturer.
Liability or obligation on the part of Hyd·Mech for damages, whether general, special or for negligence and expressly
including any incidental and consequential damages is hereby disclaimed. Hyd·Mech’s obligation to repair or replace shall
be the limit of its liability under this warranty and the sole and exclusive right and remedy of the user.
THIS WARRANTY IS EXPRESSLY IN LIEU OF ALL OTHER WARRANTIES, EXPRESSED OR IMPLIED, WRITTEN OR
ORAL, INCLUDING WITHOUT LIMITATION ANY IMPLIED WARRANTIES OF MERCHANTABILITY OR FITNESS FOR
A PARTICULAR PURPOSE.
This warranty may not be changed, altered, or modied in any way except in writing by Hyd-Mech
Group Limited
HYD·MECH GROUP LIMITED
1079 Parkinson Road
P.O. BOX 1659
Woodstock, Ontario
N4S 0A9
Phone: (519) 539-6341
Fax: (519) 539-5126
Toll Free: (877) 276-SAWS (7297)
E-mail: [email protected]
9.1
Page 57
 Loading...