

Page 1
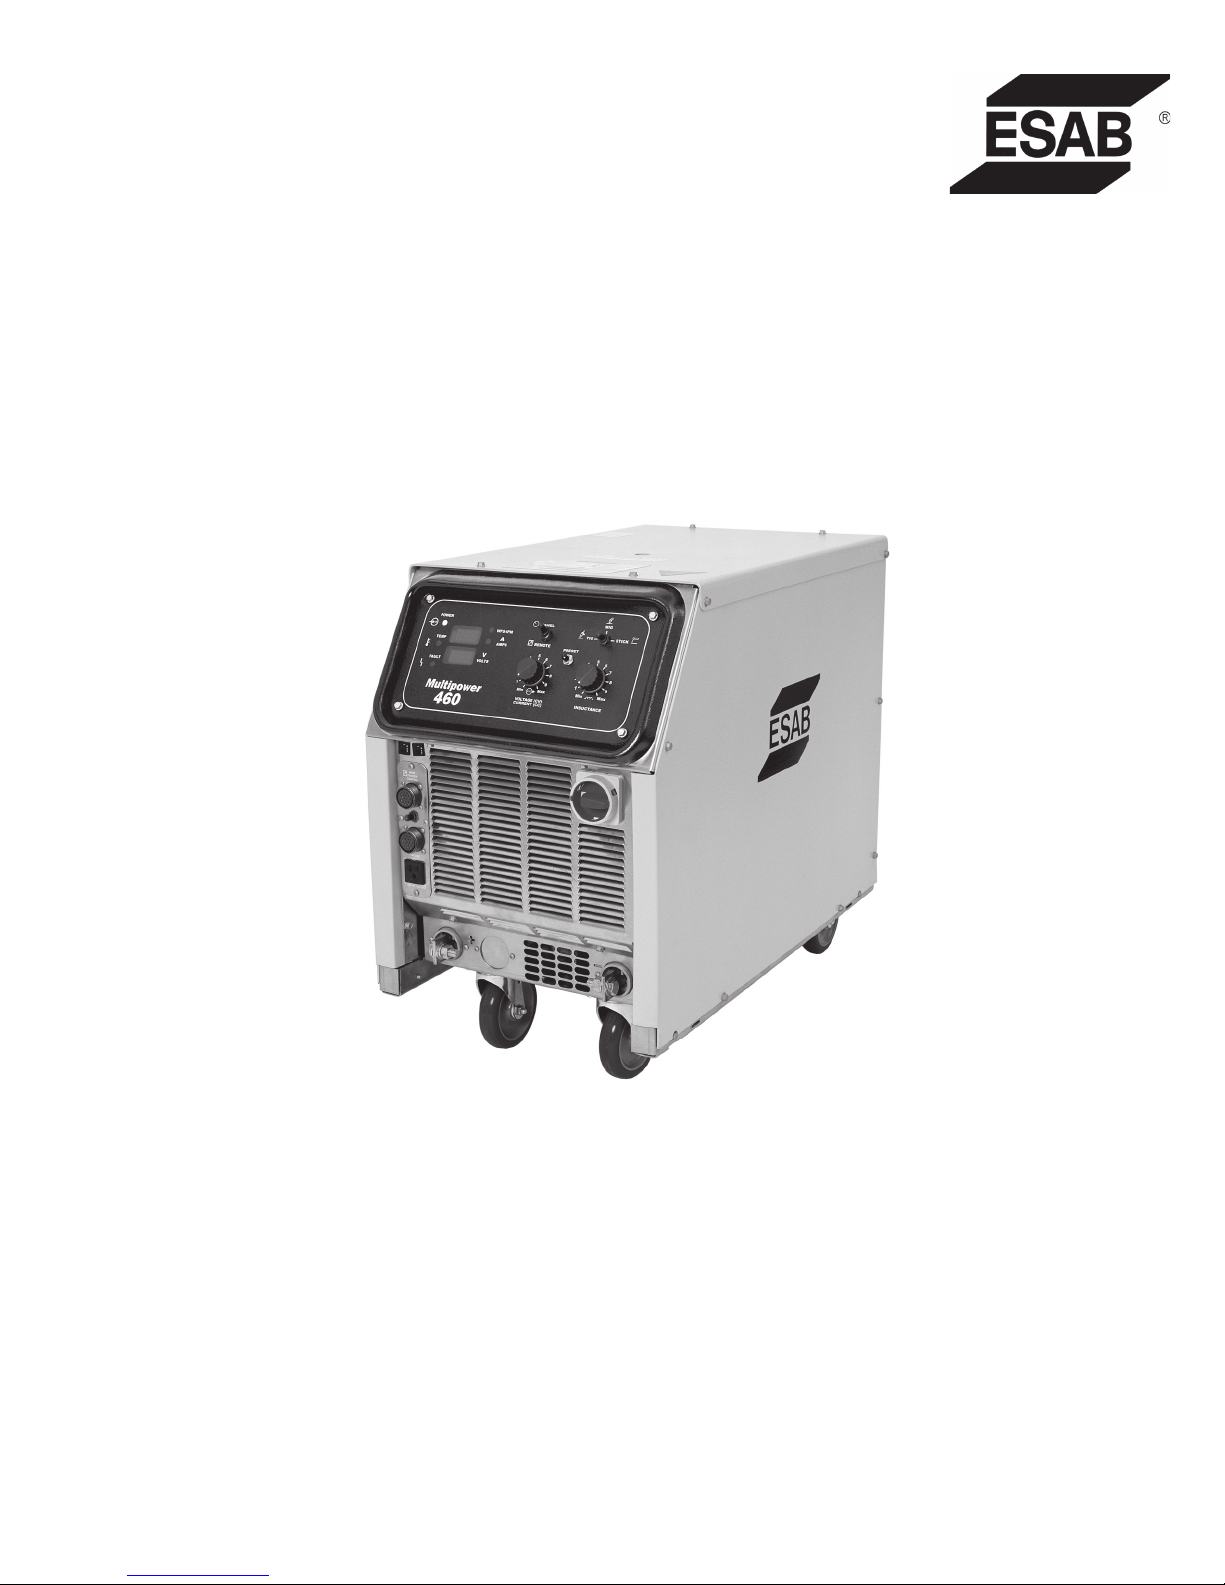
MultiPow er 460
DC Welding Power Source
This manual provides complete instructions for the following power sources starting with Serial Number MORJ143001,
October 2001:
ESAB ITEM NO. 0558002669, MultiPower 460cvcc - 230/460/575 vac, 3 ph., 60 Hz
Instruction Manual
F15-666-A 07 / 2003
Page 2
BE SURE THIS INFORMATION REACHES THE OPERATOR
These INSTRUCTIONS are for experienced operators. If you are not fully familiar with
the principles of operation and safe practices for arc welding and cutting equipment,
we urge you to read our booklet, "Precautions and Safe Practices for Arc Welding,
Cutting, and Gouging," Form 52-529. Do NOT permit untrained persons to install,
operate, or maintain this equipment. Do NOT attempt to install or operate this
equipment until you have read and fully understand these instructions. If you do not
fully understand these instructions, contact your supplier for further information. Be
sure to read the Safety Precautions before installing or operating this equipment.
USER RESPONSIBILITY
This equipment will perform in conformity with the description thereof contained in this manual and
accompanying labels and/or inserts when installed, operated, maintained and repaired in accordance
with the instructions provided. This equipment must be checked periodically. Malfunctioning or poorly
maintained equipment should not be used. Parts that are broken, missing, worn, distorted or
contaminated should be replaced immediately. Should such repair or replacement become
necessary, the manufacturer recommends that a telephone or written request for service advice be
made to the Authorized Distributor from whom it was purchased.
This equipment or any of its parts should not be altered without the prior written approval of the
manufacturer. The user of this equipment shall have the sole responsibility for any malfunction which
results from improper use, faulty maintenance, damage, improper repair or alteration by anyone other
than the manufacturer or a service facility designated by the manufacturer.
Copies of this manual can be obtained by any of the following;
Contacting your local ESAB supplier.
Downloading a copy from the ESAB web site at
ESAB WELDING & CUTTING PRODUCTS
www.esabna.com
Sending a written request to
ATTN: LITERATURE DEPT.
411 S EBENEZER ROAD
FLORENCE SC 29501
2
Page 3
TABLE OF CONTENTS
SECTION TITLE PAGE
SECTION 1 SAFETY ..............................................................................................................................................10
SECTION 2 DESCRIPTION .................................................................................................................................... 10
SECTION 3 OPTIONAL EQUIPMENT & ACCESSORIES ..................................................................................... 15
SECTION 4 INSTALLATION .................................................................................................................................16
SECTION 5 OPER ATION.......................................................................................................................................19
SECTION 6 MAINTENANCE..................................................................................................................................24
SECTION 7 TROUBLESHOOTING ........................................................................................................................25
SECTION 8 REPLACEMENT PARTS....................................................................................................................27
3
Page 4
SAFETY PRECAUTIONS
WARNING: These Safety Precautions are for
your protection. They summarize precautionary information from the references listed in
Additional Safety Information section. Before
performing any installation or operating procedures, be
sure to read and follow the safety precautions listed below
as well as all other manuals, material safety data sheets,
labels, etc. Failure to observe Safety Precautions can result
in injury or death.
PROTECT YOURSELF AND OTHERS
Some welding, cutting, and gouging
processes are noisy and require ear
protection. The arc, like the sun, emits
ultraviolet (UV) and other radiation and
can injure skin and eyes. Hot metal can cause burns.
Training in the proper use of the processes and equipment is essential to prevent accidents. Therefore:
1. Always wear safety glasses with side shields in any work
area, even if welding helmets, face shields, and goggles
are also required.
2. Use a face shield fitted with the correct filter and cover
plates to protect your eyes, face, neck, and ears from
sparks and rays of the arc when operating or observing
operations. Warn bystanders not to watch the arc and
not to expose themselves to the rays of the electric-arc
or hot metal.
3. Wear flameproof gauntlet type gloves, heavy long-sleeve
shirt, cuffless trousers, high-topped shoes, and a welding helmet or cap for hair protection, to protect against
arc rays and hot sparks or hot metal. A flameproof apron
may also be desirable as protection against radiated
heat and sparks.
4. Hot sparks or metal can lodge in rolled up sleeves,
trouser cuffs, or pockets. Sleeves and collars should be
kept buttoned, and open pockets eliminated from the
front of clothing
5. Protect other personnel from arc rays and hot sparks
with a suitable nonflammable partition or curtains.
6. Use goggles over safety glasses when chipping slag or
grinding. Chipped slag may be hot and can fly far.
Bystanders should also wear goggles over safety glasses.
FIRES AND EXPLOSIONS -- Heat from
flames and arcs can start fires. Hot slag
or sparks can also cause fires and explosions. Therefore:
1. Remove all combustible materials well away from the
work area or cover the materials with a protective nonflammable covering. Combustible materials include
wood, cloth, sawdust, liquid and gas fuels, solvents,
paints and coatings, paper, etc.
2. Hot sparks or hot metal can fall through cracks or
crevices in floors or wall openings and cause a hidden
smoldering fire or fires on the floor below. Make certain
that such openings are protected from hot sparks and
metal.“
3. Do not weld, cut or perform other hot work until the
workpiece has been completely cleaned so that there
are no substances on the workpiece which might produce flammable or toxic vapors. Do not do hot work on
closed containers. They may explode.
4. Have fire extinguishing equipment handy for instant use,
such as a garden hose, water pail, sand bucket, or
portable fire extinguisher. Be sure you are trained in its
use.
F-15-660
5. Do not use equipment beyond its ratings. For example,
overloaded welding cable can overheat and create a fire
hazard.
6. After completing operations, inspect the work area to
make certain there are no hot sparks or hot metal which
could cause a later fire. Use fire watchers when necessary.
7. For additional information, refer to NFPA Standard 51B,
"Fire Prevention in Use of Cutting and Welding Pro-
--
cesses", available from the National Fire Protection Association, Batterymarch Park, Quincy, MA 02269.
ELECTRICAL SHOCK -- Contact with live
electrical parts and ground can cause
severe injury or death. DO NOT use AC
welding current in damp areas, if movement is confined, or if there is danger of
falling.
1. Be sure the power source frame (chassis) is connected
to the ground system of the input power.
2. Connect the workpiece to a good electrical ground.
3. Connect the work cable to the workpiece. A poor or
missing connection can expose you or others to a fatal
shock.
4. Use well-maintained equipment. Replace worn or damaged cables.
5. Keep everything dry, including clothing, work area, cables,
torch/electrode holder, and power source.
6. Make sure that all parts of your body are insulated from
work
and from ground.
7. Do not stand directly on metal or the earth while working
in tight quarters or a damp area; stand on dry boards or
an insulating platform and wear rubber-soled shoes.
8. Put on dry, hole-free gloves before turning on the power.
9. Turn off the power before removing your gloves.
10. Refer to ANSI/ASC Standard Z49.1 (listed on next page)
for specific grounding recommendations. Do not mistake
the work lead for a ground cable.
ELECTRIC AND MAGNETIC FIELDS —
May be dangerous. Electric current flowing through any conductor causes localized Electric and Magnetic Fields
(EMF). Welding and cutting current creates EMF around welding cables and
welding machines. Therefore:
1. Welders having pacemakers should consult their physician before welding. EMF may interfere with some pacemakers.
2. Exposure to EMF may have other health effects which are
unknown.
3. Welders should use the following procedures to minimize
exposure to EMF:
A. Route the electrode and work cables together. Secure
them with tape when possible.
B. Never coil the torch or work cable around your body.
C. Do not place your body between the torch and work
cables. Route cables on the same side of your body.
D. Connect the work cable to the workpiece as close as
possible to the area being welded.
E. Keep welding power source and cables as far away
from your body as possible.
10/98
4
Page 5
SAFETY PRECAUTIONS
FUMES AND GASES -- Fumes and
gases, can cause discomfort or harm,
particularly in confined spaces. Do
not breathe fumes and gases. Shielding gases can cause asphyxiation.
Therefore:
1. Always provide adequate ventilation in the work area by
natural or mechanical means. Do not weld, cut, or gouge
on materials such as galvanized steel, stainless steel,
copper, zinc, lead, beryllium, or cadmium unless positive
mechanical ventilation is provided. Do not breathe fumes
from these materials.
2. Do not operate near degreasing and spraying operations. The heat or arc rays can react with chlorinated
hydrocarbon vapors to form phosgene, a highly toxic
gas, and other irritant gases.
3. If you develop momentary eye, nose, or throat irritation
while operating, this is an indication that ventilation is not
adequate. Stop work and take necessary steps to improve ventilation in the work area. Do not continue to
operate if physical discomfort persists.
4. Refer to ANSI/ASC Standard Z49.1 (see listing below)
for specific ventilation recommendations.
5. WARNING: This product, when used for welding or
cutting, produces fumes or gases which
contain chemicals known to the State of
California to cause birth defects and, in
some cases, cancer. (California Health &
Safety Code
CYLINDER HANDLING -- Cylinders, if
mishandled, can rupture and violently
release gas. Sudden rupture of cylinder, valve, or relief device can injure or
kill. Therefore:
1. Use the proper gas for the process and use the proper
pressure reducing regulator designed to operate from
the compressed gas cylinder. Do not use adaptors.
Maintain hoses and fittings in good condition. Follow
manufacturer's operating instructions for mounting regulator to a compressed gas cylinder.
2. Always secure cylinders in an upright position by chain
or strap to suitable hand trucks, undercarriages, benches,
walls, post, or racks. Never secure cylinders to work
tables or fixtures where they may become part of an
electrical circuit.
3. When not in use, keep cylinder valves closed. Have
valve protection cap in place if regulator is not connected. Secure and move cylinders by using suitable
hand trucks. Avoid rough handling of cylinders.
4. Locate cylinders away from heat, sparks, and flames.
Never strike an arc on a cylinder.
5. For additional information, refer to CGA Standard P-1,
"Precautions for Safe Handling of Compressed Gases in
Cylinders", which is available from Compressed Gas
Association, 1235 Jefferson Davis Highway, Arlington,
VA 22202.
§25249.5 et seq.)
EQUIPMENT MAINTENANCE -- Faulty or
improperly maintained equipment can
cause injury or death. Therefore:
1. Always have qualified personnel perform the installation, troubleshooting, and maintenance work. Do not
perform any electrical work unless you are qualified to
perform such work.
2. Before performing any maintenance work inside a power
source, disconnect the power source from the incoming
electrical power.
3. Maintain cables, grounding wire, connections, power
cord, and power supply in safe working order. Do not
operate any equipment in faulty condition.
4. Do not abuse any equipment or accessories. Keep
equipment away from heat sources such as furnaces,
wet conditions such as water puddles, oil or grease,
corrosive atmospheres and inclement weather.
5. Keep all safety devices and cabinet covers in position
and in good repair.
6. Use equipment only for its intended purpose. Do not
modify it in any manner.
ADDITIONAL SAFETY INFORMATION -- For
more information on safe practices for electric arc welding and cutting equipment, ask
your supplier for a copy of "Precautions and
Safe Practices for Arc Welding, Cutting and
Gouging", Form 52-529.
The following publications, which are available from the
American Welding Society, 550 N.W. LeJuene Road, Miami, FL 33126, are recommended to you:
1. ANSI/ASC Z49.1 - "Safety in Welding and Cutting"
2. AWS C5.1 - "Recommended Practices for Plasma Arc
Welding"
3. AWS C5.2 - "Recommended Practices for Plasma Arc
Cutting"
4. AWS C5.3 - "Recommended Practices for Air Carbon
Arc Gouging and Cutting"
5. AWS C5.5 - "Recommended Practices for Gas Tungsten
Arc Welding“
6. AWS C5.6 - "Recommended Practices for Gas Metal Arc
Welding"“
7. AWS SP - "Safe Practices" - Reprint, Welding Handbook.
8. ANSI/AWS F4.1, "Recommended Safe Practices for
Welding and Cutting of Containers That Have Held
Hazardous Substances."
MEANING OF SYMBOLS - As used throughout this manual: Means Attention! Be Alert!
Your safety is involved.
Means immediate hazards which, if
not avoided, will result in immediate,
serious personal injury or loss of life.
Means potential hazards which could
result in personal injury or loss of life.
Means hazards which could result in
minor personal injury.
5
SP98-10
Page 6
PRECAUCION DE SEGURIDAD
ADVERTENCIA: Estas Precauciones de
Seguridad son para su protección. Ellas hacen
referencias listadas en la sección "Información Adicional Sobre La
Seguridad". Antes de hacer cualquier instalación o procedimiento
de operación , asegúrese de leer y seguir las precauciones de
seguridad listadas a continuación así como también todo manual,
hoja de datos de seguridad del material, calcomanias, etc. El no
observar las Precauciones de Seguridad puede resultar en daño
resumen de información proveniente de las
a la persona o muerte
.
PROTEJASE USTED Y A LOS DEMAS
Algunos procesos de soldadura, corte y
ranurado son ruidosos y requiren
protección para los oídos. El arco, como
el sol , emite rayos ultravioleta (UV) y otras radiaciones
que pueden dañar la piel y los ojos. El metal caliente causa
quemaduras. EL entrenamiento en el uso propio de los
equipos y sus procesos es esencial para prevenir
accidentes. Por lo tanto:
1.
Utilice gafas de seguridad con protección a los lados siempre que
esté en el área de trabajo, aún cuando esté usando careta de
soldar, protector para su cara u otro tipo de protección.
2. Use una careta que tenga el filtro correcto y lente para proteger
sus ojos, cara, cuello, y oídos de las chispas y rayos del arco
cuando se esté operando y observando las operaciones. Alerte
a todas las personas cercanas de no mirar el arco y no
exponerse a los rayos del arco eléctrico o el metal fundido.
3. Use guantes de cuero a prueba de fuego, camisa pesada de
mangas largas, pantalón de ruedo liso, zapato alto al tobillo, y
careta de soldar con capucha para el pelo, para proteger el
cuerpo de los rayos y chispas calientes provenientes del metal
fundido. En ocaciones un delantal a prueba de fuego es
necesario para protegerse del calor radiado y las chispas.
4. Chispas y partículas de metal caliente puede alojarse en las
mangas enrolladas de la camisa , el ruedo del pantalón o los
bolsillos. Mangas y cuellos deberán mantenerse abotonados,
bolsillos al frente de la camisa deberán ser cerrados o eliminados.
5. Proteja a otras personas de los rayos del arco y chispas
calientes con una cortina adecuada no-flamable como división.
6. Use careta protectora además de sus gafas de seguridad
cuando esté removiendo escoria o puliendo. La escoria puede
estar caliente y desprenderse con velocidad. Personas cercanas
deberán usar gafas de seguridad y careta
protectora.
FUEGO Y EXPLOSIONES -- El calor de
las flamas y el arco pueden ocacionar
fuegos. Escoria caliente y las chispas
pueden causar fuegos y explosiones. Por lo tanto:
1.
Remueva todo material combustible lejos del área de trabajo o
cubra los materiales con una cobija a prueba de fuego. Materiales
combustibles incluyen madera, ropa, líquidos y gases flamables,
solventes, pinturas, papel, etc.
2. Chispas y partículas de metal pueden introducirse en las grietas
y agujeros de pisos y paredes causando fuegos escondidos en
otros niveles o espacios. Asegúrese de que toda grieta y agujero
esté cubierto para proteger lugares adyacentes contra fuegos.
3. No corte, suelde o haga cualquier otro trabajo relacionado hasta
que la pieza de trabajo esté totalmente limpia y libre de substancias
que puedan producir gases inflamables o vapores tóxicos. No
trabaje dentro o fuera de contenedores o tanques cerrados.
Estos pueden explotar si contienen vapores inflamables.
4. Tenga siempre a la mano equipo extintor de fuego para uso
instantáneo, como por ejemplo una manguera con agua, cubeta
con agua, cubeta con arena, o extintor portátil. Asegúrese que
usted esta entrenado para su uso.
5. No use el equipo fuera de su rango de operación. Por ejemplo, el calor
causado por cable sobrecarga en los cables de soldar pueden
ocasionar un fuego.
6. Después de termirar la operación del equipo, inspeccione el área de
trabajo para cerciorarse de que las chispas o metal caliente
ocasionen un fuego más tarde. Tenga personal asignado para vigilar
si es necesario.
7. Para información adicional , haga referencia a la publicación NFPA
Standard 51B, "Fire Prevention in Use of Cutting and Welding
Processes", disponible a través de la National Fire Protection
Association, Batterymarch Park, Quincy, MA 02269.
--
CHOQUE ELECTRICO -- El contacto con
las partes eléctricas energizadas y tierra
puede causar daño severo o muerte. NO
use soldadura de corriente alterna (AC) en
áreas húmedas, de movimiento confinado
en lugares estrechos o si hay
posibilidad de caer al suelo.
1.
Asegúrese de que el chasis de la fuente de poder esté conectado
a tierra através del sistema de electricidad primario.
2. Conecte la pieza de trabajo a un buen sistema de tierra física.
3. Conecte el cable de retorno a la pieza de trabajo. Cables y
conductores expuestos o con malas conexiones pueden exponer
al operador u otras personas a un choque eléctrico fatal.
4. Use el equipo solamente si está en buenas condiciones. Reemplaze
cables rotos, dañados o con conductores expuestos.
5. Mantenga todo seco, incluyendo su ropa, el área de trabajo, los
cables, antorchas, pinza del electrodo, y la fuente de poder.
6. Asegúrese que todas las partes de su cuerpo están insuladas de
ambos, la pieza de trabajo y tierra.
7. No se pare directamente sobre metal o tierra mientras trabaja en
lugares estrechos o áreas húmedas; trabaje sobre un pedazo de
madera seco o una plataforma insulada y use zapatos con suela
de goma.
8. Use guantes secos y sin agujeros antes de energizar el equipo.
9. Apage el equipo antes de quitarse sus guantes.
10. Use como referencia la publicación ANSI/ASC Standard Z49.1
(listado en la próxima página) para recomendaciones específicas
de como conectar el equipo a tierra. No confunda el cable de soldar
a la pieza de trabajo con el cable a tierra.
CAMPOS ELECTRICOS Y MAGNETICOS
- Son peligrosos. La corriente eléctrica
fluye através de cualquier conductor
causando a nivel local Campos Eléctricos
y Magnéticos (EMF). Las corrientes en el
área de corte y soldadura, crean EMF
alrrededor de los cables de soldar y las
maquinas. Por lo tanto:
1. S
oldadores u Operadores que use marca-pasos para el corazón
deberán consultar a su médico antes de soldar. El Campo
Electromagnético (EMF) puede interferir con algunos marca-pasos.
2. Exponerse a campos electromagnéticos (EMF) puede causar otros
efectos de salud aún desconocidos.
3. Los soldadores deberán usar los siguientes procedimientos para
minimizar exponerse al EMF:
A. Mantenga el electrodo y el cable a la pieza de trabajo juntos, hasta
llegar a la pieza que usted quiere soldar. Asegúrelos uno junto al
otro con cinta adhesiva cuando sea posible.
B. Nunca envuelva los cables de soldar alrededor de su cuerpo.
C. Nunca ubique su cuerpo entre la antorcha y el cable, a la pieza
de trabajo. Mantega los cables a un sólo lado de su cuerpo.
D. Conecte el cable de trabajo a la pieza de trabajo lo más cercano
posible al área de la soldadura.
E. Mantenga la fuente de poder y los cables de soldar lo más lejos
posible de su cuerpo.
6
Page 7
HUMO Y GASES -- El humo y los gases,
pueden causar malestar o daño,
particularmente en espacios sin
ventilación. No inhale el humo o gases. El
gas de protección puede causar falta de
oxígeno. Por lo tanto:
1. Siempre provea ventilación adecuada en el área de trabajo
por medio natural o mecánico. No solde, corte, o ranure
materiales con hierro galvanizado, acero inoxidable,
cobre, zinc, plomo, berílio, o cadmio a menos que provea
ventilación mecánica positiva . No respire los gases
producidos por estos materiales.
2. No opere cerca de lugares donde se aplique substancias
químicas en aerosol. El calor de los rayos del arco pueden
reaccionar con los vapores de hidrocarburo clorinado para
formar un fosfógeno, o gas tóxico, y otros irritant es.
3. Si momentáneamente desarrolla inrritación de ojos, nariz
o garganta mientras est á operando, es indicación de que
la ventilación no es apropiada. Pare de trabajar y tome
las medidas necesarias para mejorar la ventilación en
el área de trabajo. No continúe operando si el malestar
físico persiste.
4. Haga referencia a la publicación ANSI/ASC Standard Z49.1
(Vea la lista a continuación) para recomendaciones
específicas en la ventilación.
5. ADVERTENCIA-- Este producto cuando se utiliza para
soldaduras o cortes, produce humos
o gases, los cuales contienen químicos
conocidos por el Estado de California
de causar defectos en el nacimiento, o
en algunos casos, Cancer. (California
Health & Safety Code
MANEJO DE CILINDROS-- Los
cilindros, si no son manejados
correctamente, pueden romperse y
liberar violentamente gases. Rotura
repentina del cilindro, válvula, o
válvula de escape puede causar daño
o muerte. Por lo tanto:
1. Utilize el gas apropiado para el proceso y utilize un
regulador diseñado para operar y reducir la presión del
cilindro de gas . No utilice adaptadores. Mantenga las
mangueras y las conexiones en buenas condiciones.
Observe las instrucciones de operación del manufacturero
para montar el regulador en el cilindro de gas comprimido.
2. Asegure siempre los cilindros en posición vertical y
amárrelos con una correa o cadena adecuada para
asegurar el cilindro al carro, transportes, tablilleros, paredes,
postes, o armazón. Nunca asegure los cilindros a la mesa
de trabajo o las piezas que son parte del circuito de
soldadura . Este puede ser parte del circuito elélectrico.
3. Cuando el cilindro no está en uso, mantenga la válvula del
cilindro cerrada. Ponga el capote de protección sobre la
válvula si el regulador no está conectado. Asegure y
mueva los cilindros utilizando un carro o transporte
adecuado. Evite el manejo brusco de los cilindros.
4. Localize los cilindros lejos del calor, chispas, y flamas.
Nunca establezca un arco en el cilindro.
5. Para información adicional, haga referencia a la publicación
CGA Standard P-1, "Precautions for Safe Handling of Compressed Gases in Cylinders", disponible através del Compressed Gas Association, 1235 Jefferson Davis Highway,
Arlington, VA 22202.
§25249.5 et seq.)
MANTENIMIENTO DEL EQUIPO -- Equipo
defectuoso o mal mantenido puede causar
daño o muerte. Por lo tanto:
1. Siempre tenga personal cualificado para efectuar l a
instalación, diagnóstico, y mantenimiento del equipo. No
ejecute ningún trabajo eléctrico a menos que usted esté
cualificado para hacer el trabajo.
2. Antes de dar mantenimiento en el interior de la fuente
de poder, desconecte la fuente de poder del suministro
de electricidad primaria.
3. Mantenga los cables, cable a tierra, conexciones, cable
primario, y cualquier otra fuente de poder en buen
estado operacional. No opere ningún equipo en malas
condiciones.
4. No abuse del equipo y sus accesorios. Mantenga el
equipo lejos de cosas que generen calor como hornos,
también lugares húmedos como charcos de agua , aceite
o grasa, atmósferas corrosivas y las inclemencias del
tiempo.
5. Mantenga todos los artículos de seguridad y coverturas
del equipo en su posición y en buenas condiciones.
6. Use el equipo sólo para el propósito que fue diseñado.
No modifique el equipo en ninguna manera.
INFORMACION ADICIONAL DE SEGURIDAD
-- Para más información sobre las prácticas de
seguridad de los equipos de arco eléctrico para
soldar y cortar, pregunte a su suplidor por una
copia de "Precautions and Safe Practices for
Arc Welding, Cutting and Gouging-Form 52-529.
Las siguientes publicaciones, disponibles através de la
American Welding Society, 550 N.W. LeJuene Road, Miami,
FL 33126, son recomendadas para usted:
1. ANSI/ASC Z49.1 - "Safety in Welding and Cutting"
2. AWS C5.1 - "Recommended Practices for Plasma Arc
Welding"
3. AWS C5.2 - "Recommended Practices for Plasma Arc
Cutting"
4. AWS C5.3 - "Recommended Practices for Air Carbon Arc
Gouging and Cutting"
5. AWS C5.5 - "Recommended Practices for Gas Tungsten
Arc Welding“
6. AWS C5.6 - "Recommended Practices for Gas Metal Arc
Welding"“
7. AWS SP - "Safe Practices" - Reprint, Welding Handbook.
8. ANSI/AWS F4.1, "Recommended Safe Practices for Welding and Cutting of Containers That Have Held Hazardous
Substances."
SIGNIFICADO DE LOS SIMBOLOS -Según usted avanza en la lectura de
este folleto: Los Símbolos Significan
¡Atención! ¡Esté Alerta! Se trata de su
seguridad.
Significa riesgo inmediato que, de no ser
evadido, puede resultar inmediatamente
en serio daño personal o la muerte.
Significa el riesgo de un peligro potencial
que puede resultar en serio daño personal o la muerte.
Significa el posible riesgo que puede
resultar en menores daños a la persona.
7
Page 8
PRÉCAUTIONS DE SÉCURITÉ
AVERTISSEMENT: Ces règles de sécurité ont pour objet
d’ assurer votre protection. Veillez à lire et à observer les
précautions énoncées ci-dessous avant de monter l’
équipement ou de commercer à l’utiliser. Tout défaut
d’observation de ces précautions risque d’entraîner des
blessures graves ou mortelles.
1. PROTECTION INDIVIDUELLE-- Les brûlures de la
peau et des yeux dues au rayonnement de l’arc
électrique ou du métal incandescent, lors du soudage
au plasma ou à l’électrode ou lors du gougeage à
l’arc, peuvent s’avérer plus graves que celles
résultant d’une exposition prolongée au soleil. Aussi
convient-il d’observer les précautions suivantes:
a. Portez un écran facial adéquat muni des plaques
protectrices et des verres filtrants appropriés afin de
vous protéger les yeux, le visage, le cou et les oreilles
des étincelles et du rayonnement de l’arc électrique
lorsque vous effectuez des soudures ou des coupes
ou lorsque vous en observez l’exécution.
AVERTISSEZ les personnes se trouvant à proximité
de façon à ce qu’elles ne regardent pas l’arc et à ce
qu’elles ne s’exposent pas à son rayonnement, ni à
celui du métal incandescent.
b. Portez des gants ignifugés à crispins, une tunique
épaisse à manches longues, des pantalons sans
rebord, des chaussures à embout d’acier et un
casque de soudage ou une calotte de protection, afin
d’éviter d’exposer la peau au rayonnement de l’arc
électrique ou du métal incandescent. ll est également
souhaitable d’utiliser un tablier ininflammable de
façon à se protéger des étincelles et du rayonnement
thermique.
c. Les étincelles ou les projections de métal incandes-
cent risquent de se loger dans des manches
retroussées, des bords relevés de pantalons ou dans
des poches. Aussi convient-il de garder boutonnés le
col et les manches et de porter des vêtements sans
poches à l’avant.
d. Protégez des étincelles et du rayonnement de l’arc
électrique les autres personnes travaillant à proximité
à l’aide d’un écran ininflammable adéquat.
e. Ne jamais omettre de porter des lunettes de sécurité
lorsque vous vous trouvez dans un secteur où l’on
effectue des opérations de soudage ou de coupage à
l’arc. Utilisez des lunettes de sécurité à écrans ou
verres latéraux pour piquer ou meûler le laitier. Les
piquetures incandescentes de laitier peuvent être
projetées à des distances considérables. Les
personnes se trouvant à proximité doivent également
porter des lunettes de protection.
f. Le gougeage à l’arc et le soudage à l’arc au plasma
produisent un niveau de bruit extrêmement élevé (de
100 à 114 dB) et exigent par conséquent l’emploi de
dispositifs appropriés de protection auditive.
2. PRÉVENTION DES INCENDES-- Les projections de
laitier incandescent ou d’étincelles peuvent
provoquer de graves incendies au contact de
matériaux combustibles solides, liquides ou gazeux.
Aussi faut-il observer les précautions suivantes:
a. Éloigner suffisamment tous les matériaux combus-
tibles du secteur où l’on exécute des soudures ou des
coupes à l’arc, à moins de les recouvrir complètement
d’une bâche non-inflammable. Ce type de matériaux
comprend notamment le bois, les vêtements, la sciure,
l’essence, le kérosène, les peintures, les solvants, le
gaz naturel, l’acétylène, le propane et autres substances combustibles semblables.
b. Les étincelles ou les projections de métal incandes-
cent peuvent tomber dans des fissures du plancher ou
dans des ouvertures des murs et y déclencher une
ignition lente cachée. Veiller à protéger ces ouvertures
des étincelles et des projections de métal.
c. N’exécutez pas de soudures, de coupes, d’opérations
de gougeage ou autres travaux à chaud à la surface
de barils, bidons, réservoirs ou autres contenants
usagés, avant de les avoir nettoyés de toute trace de
substance susceptible de produire des vapeurs
inflammables ou toxiques.
d. En vue d’assurer la prévention des incendies, il
convient de disposer d’un matériel d’extinction prêt à
servir immédiatement, tel qu’un tuyau d’arrosage, un
seau à eau, un seau de sable ou un extincteur portatif.
e. Une fois le travail à l’arc terminé, inspectez le secteur
de façon à vous assurer qu’aucune étincelle ou projection de métal incandescent ne risque de provoquer
ultérieurement un feu.
3. CHOC ÉLECTRIQUE-- Le gougeage à l’arc et à l’arc
au plasma exige l’emploi de tensions à vide
relativement importantes; or, celles-ci risquent de
causer des dommages corporels graves et même
mortels en cas d’utilisation inadéquate. La gravité du
choc électrique reçu dépend du chemin suivi par le
courant à travers le corps humain et de son intensité.
a. Ne laissez jamais de surfaces métalliques sous ten-
sion venir au contact direct de la peau ou de
vêtements humides. Veillez à porter des gants bien
secs.
b. Si vous devez effectuer un travail sur une surface
métallique ou dans un secteur humide, veillez à assurer votre isolation corporelle en portant des gants secs
et des chaussures à semelles de caoutchouc et en
vous tenant sur une planche ou une plate-forme
sèche.
c. Mettez toujours à la terre le poste de soudage/coupage
en le reliant par un câble à une bonne prise de terre.
d. N’utilisez jamais de câbles usés ou endommagés. Ne
surchargez jamais le câble. Utilisez toujours un
équipement correctement entretenu.
e. Mettez l’équipement hors tension lorsqu’il n’est pas en
service. une mise à la masse accidentelle peut en
effet provoquer une surchauffe de l’équipement et un
danger d’incendie. Ne pas enrouler ou passer le câble
autour d’une partie quelconque du corps.
f. Vérifiez si le câble de masse est bien relié à la pièce en
un point aussi proche que possible de la zone de
travail. Le branchement des câbles de masse à
l’ossature du bâtiment ou en un point éloigné de la
zone de travail augmente en effet le risque de passage d’un courant de sortie par des chaînes de
8
9/97
Page 9
PRÉCAUTIONS DE SÉCURITÉ
levage, des câbles de grue ou divers chemins
électriques.
g. Empêchez l’apparition de toute humidité, notamment
sur vos vêtements, à la surface de l’emplacement de
travail, des câbles, du porte-électrode et du poste de
soudage/coupage. Réparez immédiatement toute
fuite d’eau.
4. VENTILATION-- La respiration prolongée des fumées
résultant des opérations de soudage/coupage, à
l’intérieur, d’un local clos, peut provoquer des malaises et des dommages corporels. Aussi convient-il
d’observer les précautions suivantes:
a. Assurez en permanence une aération adéquate de
l’emplacement de travail en maintenant une ventilation naturelle ou à l’aide de moyens mécaniques.
N’effectuez jamais de travaux de soudage ou de
coupage sur des matériaux de zinc, de plomb, de
beryllium ou de cadmium en l’absence de moyens
mécaniques de ventilation capables d’empêcher
l’inhalation des fumées dégagées par ces matériaux.
b. N’effectuez jamais de travaux de soudage ou de
coupage à proximité de vapeurs d’hydrocarbure
chloré résultant d’opérations voisines de dégraissage
ou de pulvérisation. La chaleur dégagée ou le
rayonnement de l’arc peut déclencher la formation de
phosgène -- gaz particulièrement toxique -- et d’autres
gaz irritants, à partir des vapeurs de solvant.
c. Une irritation momentanée des yeux, du nez ou de la
gorge constatée au cours de l’utilisation de
l’équipement dénote un défaut de ventilation. Arrêtezvous de travailler afin de prendre les mesures nécessaires à l’amélioration de la ventilation. Ne poursuivez
pas l’opération entreprise si le malaise persiste.
d. Certaines commandes comportent des canalisations
où circule de l’hydrogène. L’armoire de commande est
munie d’un ventilateur destiné à empêcher la formation de poches d’hydrogène, lesquelles présentent un
danger d’explosion; ce ventilateur ne fonctionne que
si l’interrupteur correspondant du panneau avant se
trouve placé en position ON (Marche). Veillez à
manœuvrer cette commande en vérifiant si le
couvercle est bien en place, de façon à assurer
l’efficacité de la ventilation ainsi réalisée. Ne jamais
débrancher le ventilateur.
e. Les fumées produites par l’opération de soudage ou
de coupage peuvent s’avérer toxiques. Aussi est-il
nécessaire de disposer en permanence d’un dispositif
adéquat de ventilation de type aspirant, afin d’éliminer du voisinage de l’opérateur tout dégagement de
fumée visible.
f. Consultez les recommandations particulières en
matière de ventilation indiquées à l’alinéa 6 de la
norme Z49.1 de l’AWS.
5. ENTRETIEN DE L’ÉQUIPEMENT-- Un équipement
entretenu de façon défectueuse ou inadéquate risque
non seulement de réaliser un travail de mauvaise
qualité mais, chose plus grave encore, d’entraîner
des dommages corporels graves, voire mortels en
déclenchant des incendies ou des chocs électriques.
Observez par conséquent les précautions suivantes:
a. Efforcez-vous de toujours confier à un personnel qua-
lifié l’installation, le dépannage et l’entretien du poste
de soudage et de coupage. N’effectuez aucune
réparation électrique sur l’équipement à moins d’être
qua-lifié à cet effet.
b. Ne procédez jamais à une tâche d’entretien
quelconque à l’intérieur du poste de soudage/
coupage, avant d’avoir débranché l’alimentation
électrique.
c. Maintenez en bon état de fonctionnement les câbles,
le câble de masse, les branchements, le cordon
d’alimentation et le poste de soudage/coupage.
N’utilisez jamais le poste ou l’équipement s’il présente
une défectuosité quelconque.
d. Prenez soin du poste de soudage et de coupage et
des équipements accessoires. Gardez-les à l’écart
des sources de charleur, notamment des fours, de
l’humidité, des flaques d’eau maintenez-les à l’abri des
traces d’huile ou de graisse, des atmosphères corrosives et des intempéries.
e. Laissez en place tous les dispositifs de sécurité et tous
les panneaux de l’armoire de commande en veillant à
les garder en bon état.
f. Utilisez le poste de soudage/coupage conformément à
son usage prévu et n’effectuez aucune modification.
6. INFORMATIONS COMPLÉMENTAIRES RELATIVES
À LA SÉCURITÉ--
Pour obtenir des informations complémentaires sur les
règles de sécurité à observer pour le montage et
l’utilisation d’équipements de soudage et de coupage
électriques et sur les méthodes de travail
recommandées, demandez un exemplaire du livret N°
52529 “Precautions and Safe Practices for Arc Welding, Cutting and Gouging” publié par ESAB. Nous
conseillons également de consulter les publications
sui-vantes, tenues à votre disposition par l’American
Welding Society, 550 N.W. LeJuene Road, Miami, FL
32126:
a. “Safety in Welding and Cutting” AWS Z49.1
b. “Recommended Safe Practices for Gas-Shielded Arc
Welding “AWS A6. 1.
c. “Safe Practices for Welding and Cutting Containers
That Have Held Combustibles” AWS-A6.0.
d. “Recommended Safe Practices for Plasma Arc Cut-
ting” AWS-A6. 3.
e. “Recommended Safe Practices for Plasma Arc Weld-
ing” AWS-C5. 1.
f. “Recommended Safe Practices for Air Carbon Arc
Gouging and Cutting” AWS-C5. 3.
g. “Code For Safety in Welding and Cutting”
CSA-Standard W117. 2.
9/97
9
Page 10
SECTION 1 & 2
SAFETY & DESCRIPTION
I. SAFETY
Before the MultiPower 460 power source is put into operation, the safety
section at the front of this manual should be read completely. This will help
avoid possible injury due to misuse or improper installation.
The definitions relating to the:
safety notations are described at the end of the Safety Section in the front of
this manual — read them and their specific text references carefully.
II. DESCRIPTION
This manual has been prepared for use by an experienced operator. It provides
information to familiarize the operator with the design, installation and operation of the MultiPower 460 power source. DO NOT attempt to install or operate
this equipment until you have read and fully understood these instructions. The
information presented here should be given careful consideration to ensure
proper installation and optimum weld performance of this equipment.
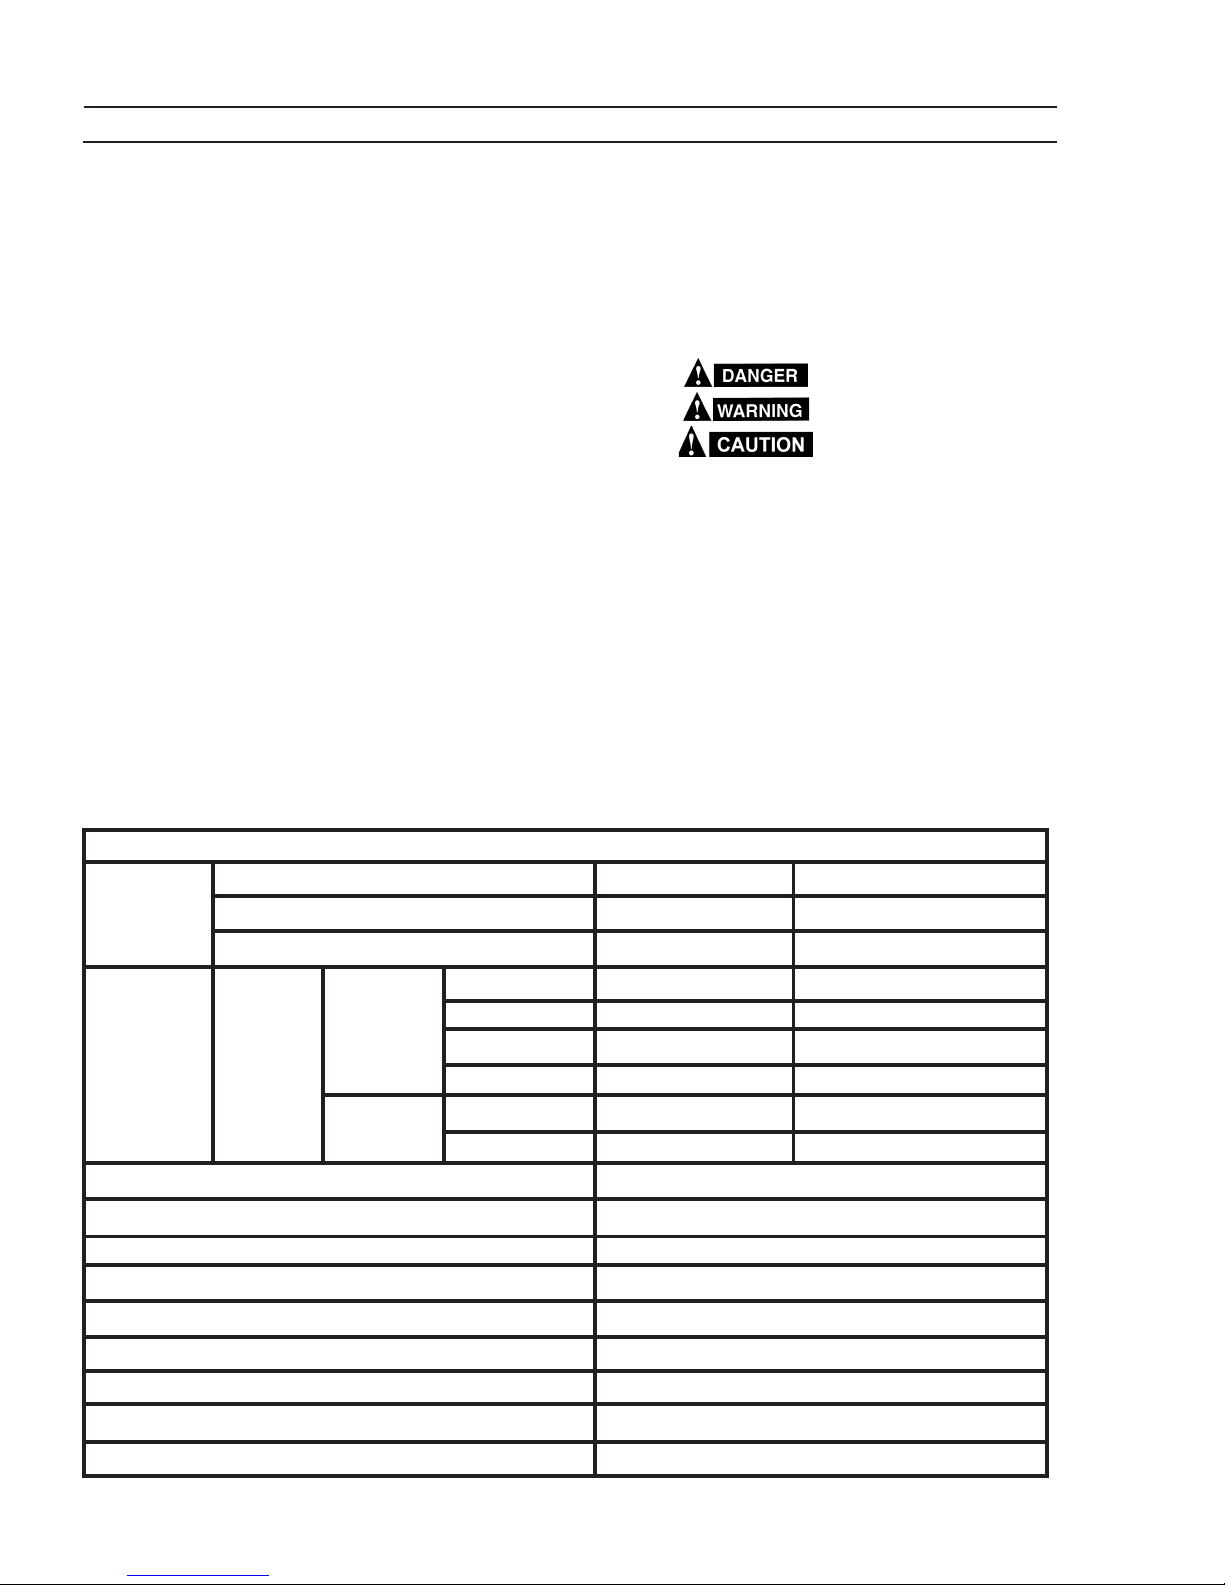
RATED
OUTPUT
RATED
INPUT
Table 2-1. Specifications for MultiPower 460
OPEN CIRCUIT VOLTAGE (U2) 80V DC Max.
DUTY CYCLE 60% 100%
Current (I
Voltage (U
60 Hz
3 Phase
50 Hz
Power Factor at Rated Output 89%
Welding Range 10 A/12 V - 500 A/40 V
Auxiliary Power 115 V ac @ 10 A, 60 Hz
PHYS ICAL SPECIFIC ATIONS
Height (without lift eye) 25.0" (62.2 cm)
Width 18.8" (48.3 cm)
Depth 32.5" (81.9 cm)
) 500 A 450 A
2
) 40 V 38 V
2
Volt s (U
208/230 V 76 A 66 A
) C urrent (I1) Flat Current (I1) Flat
1
460 V 38 A 33 A
575 V 31 A 26 A
220 V 79 A 68 A
400 V 43 A 37 A
Net Weight 322lbs (146 kg)
Shipping Weight 375lbs (170 kg)
10
Page 11
SECTION 2
DESCRIPTION
The MultiPower 460 is a multi-process power source designed for Mig short
circuiting and spray transfer (GMAW), flux core (FCAW), Tig (GTAW), and
stick (SMAW) welding and air carbon arc cutting/gouging (CAC-A) applications. Table 1-1 outlines the electrical and physical specifications.
A. POWER SOURCE
The power source is a constant current (CC) and constant voltage (CV), three
phase, secondary chopper dc design with solid state contactor and control
circuitry. It provides the volt-ampere characteristics desired for conventional
MIG and flux core arc welding in the CV (constant voltage) mode or stick
welding, Tig (GTAW) and arc gouging in the CC (constant current) mode.
Features
• Auto Fan - The MultiPower 460 fan will run when the power source is first
powered up and will raining running for 6 minutes then shut don. The fan
will start again when welding begins and is at a current level above 50 amps.
The fan will remain running for 6 minutes after welding stops and then shut
down automatically.
• Stainless steel frame for envirornmental durability.
• Durable composite side and top panels will not corrode.
• 100% duty cycle output at 460 amps.
• Mig pulse capable with Pulse Upgrade Kit.
• Compatible with all ESAB 42 vac wire feeders.
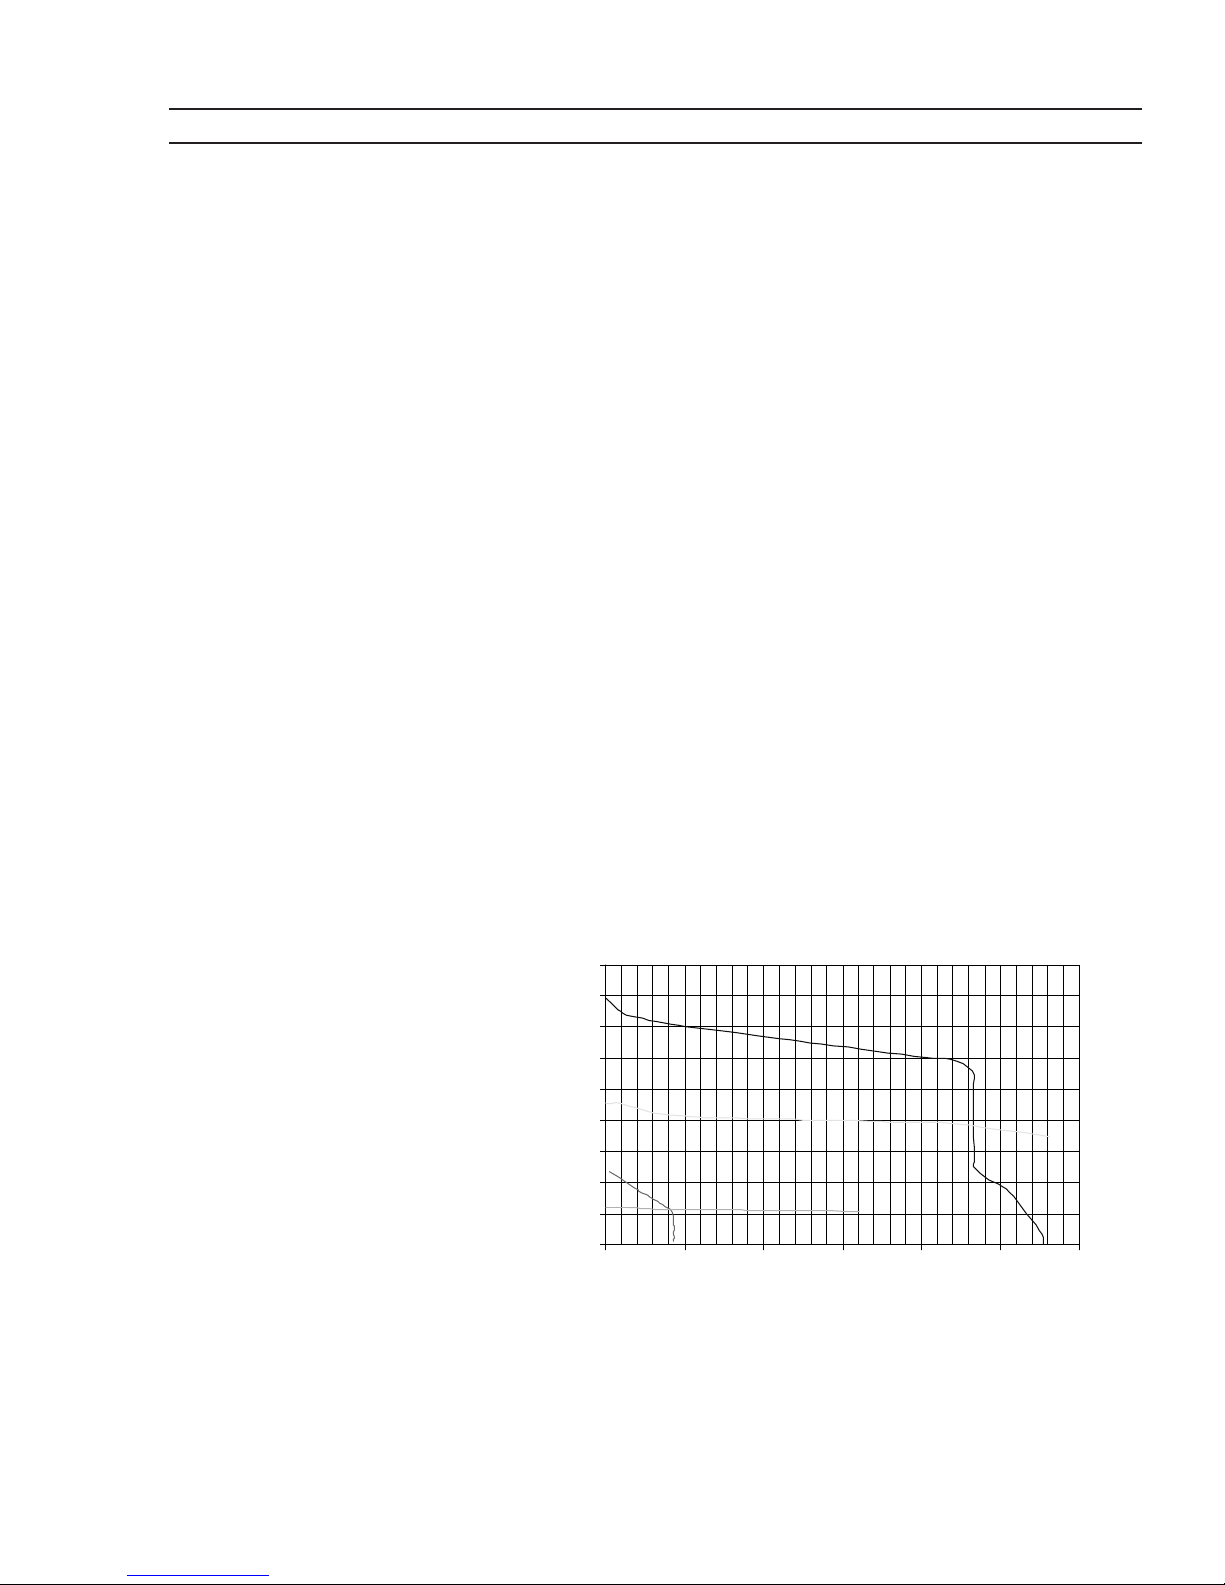
B. VOLT - AMPERE CHARACTERISTICS
The curves shown in Figure 1-1 represent the static volt-ampere characteristics
for the power source. The slant of these curves is referred to as the "slope" and
is generally defined as the voltage drop per 100 amperes of current use. These
curves show the output voltage available at any given output current from the
minimum to the maximum setting of the voltage/current control.
90
80
70
60
50
40
Arc Voltage
30
20
10
0
Constant Current
0 100 200 300 400 500 600
Constant Current
Constant Voltage
Constant Voltage
Weld Current (Amperes)
Figure 2-1 - MultiPower 460 Volt-Ampere Curves
11
Page 12
SECTION 2
DESCRIPTION
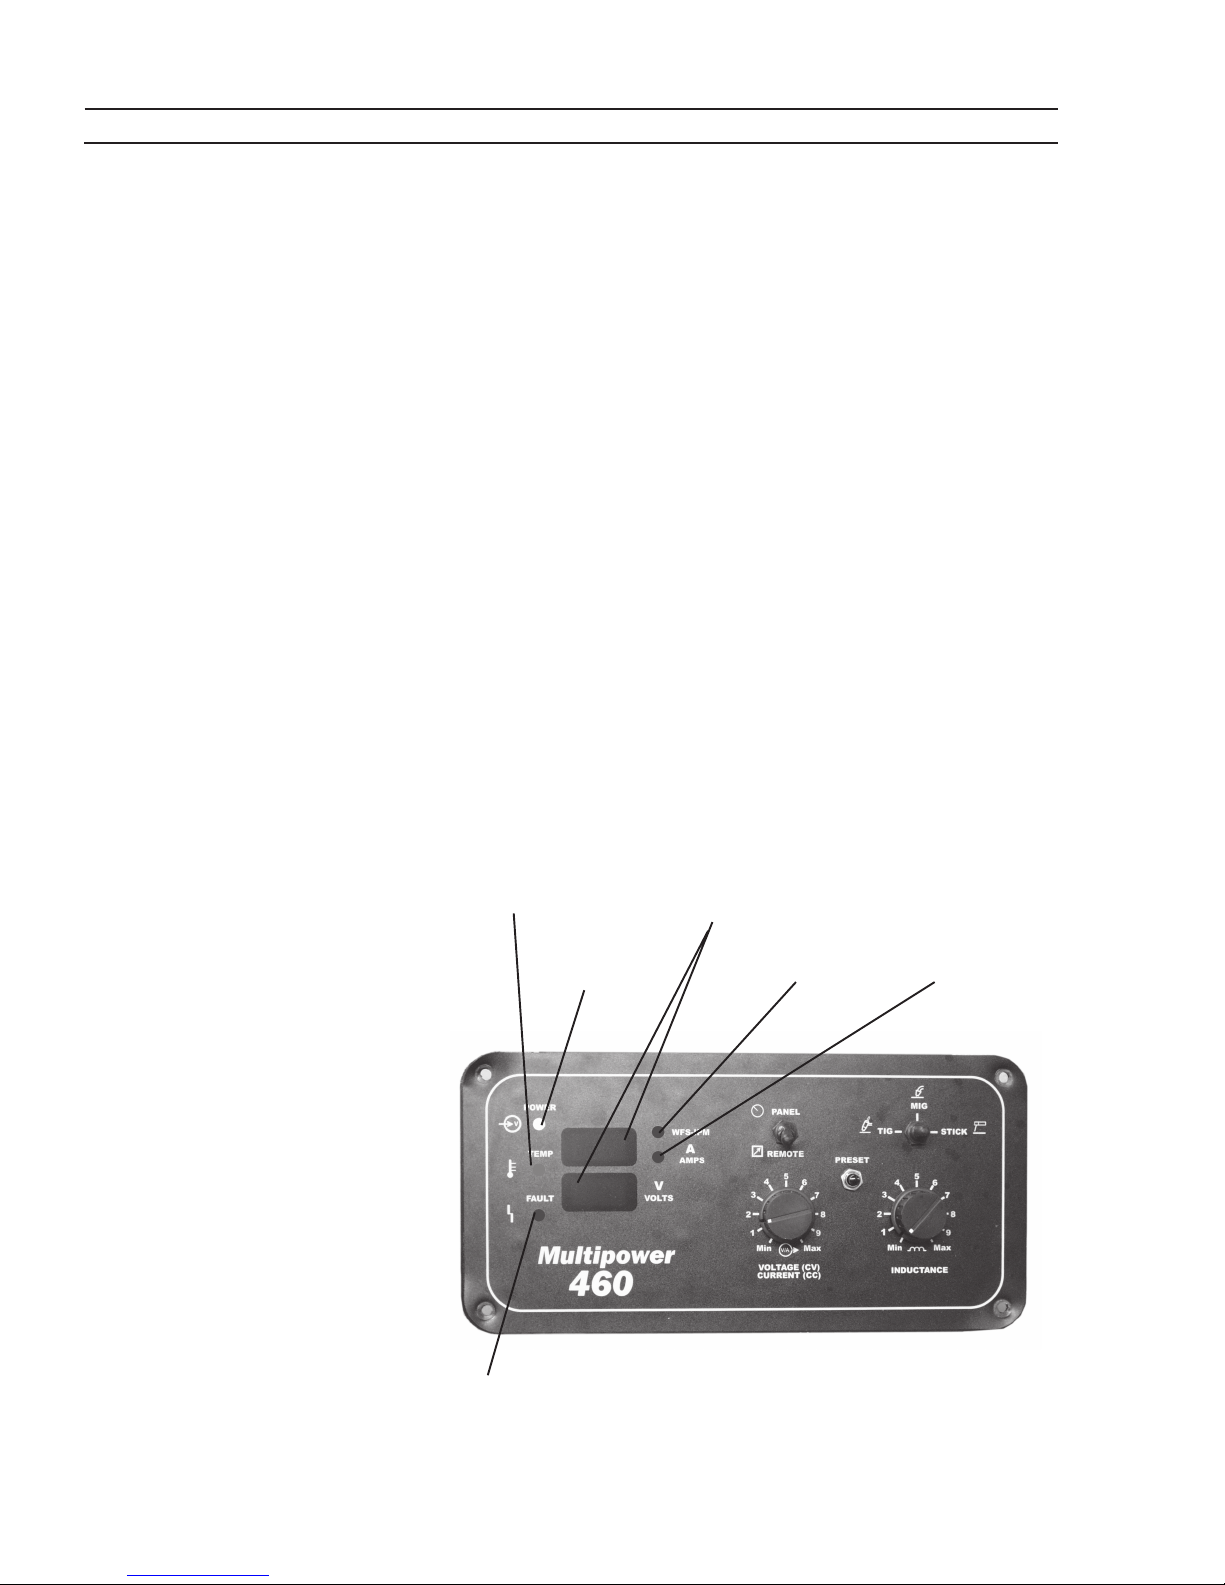
C. CONTROL PANEL DESCRIPTION
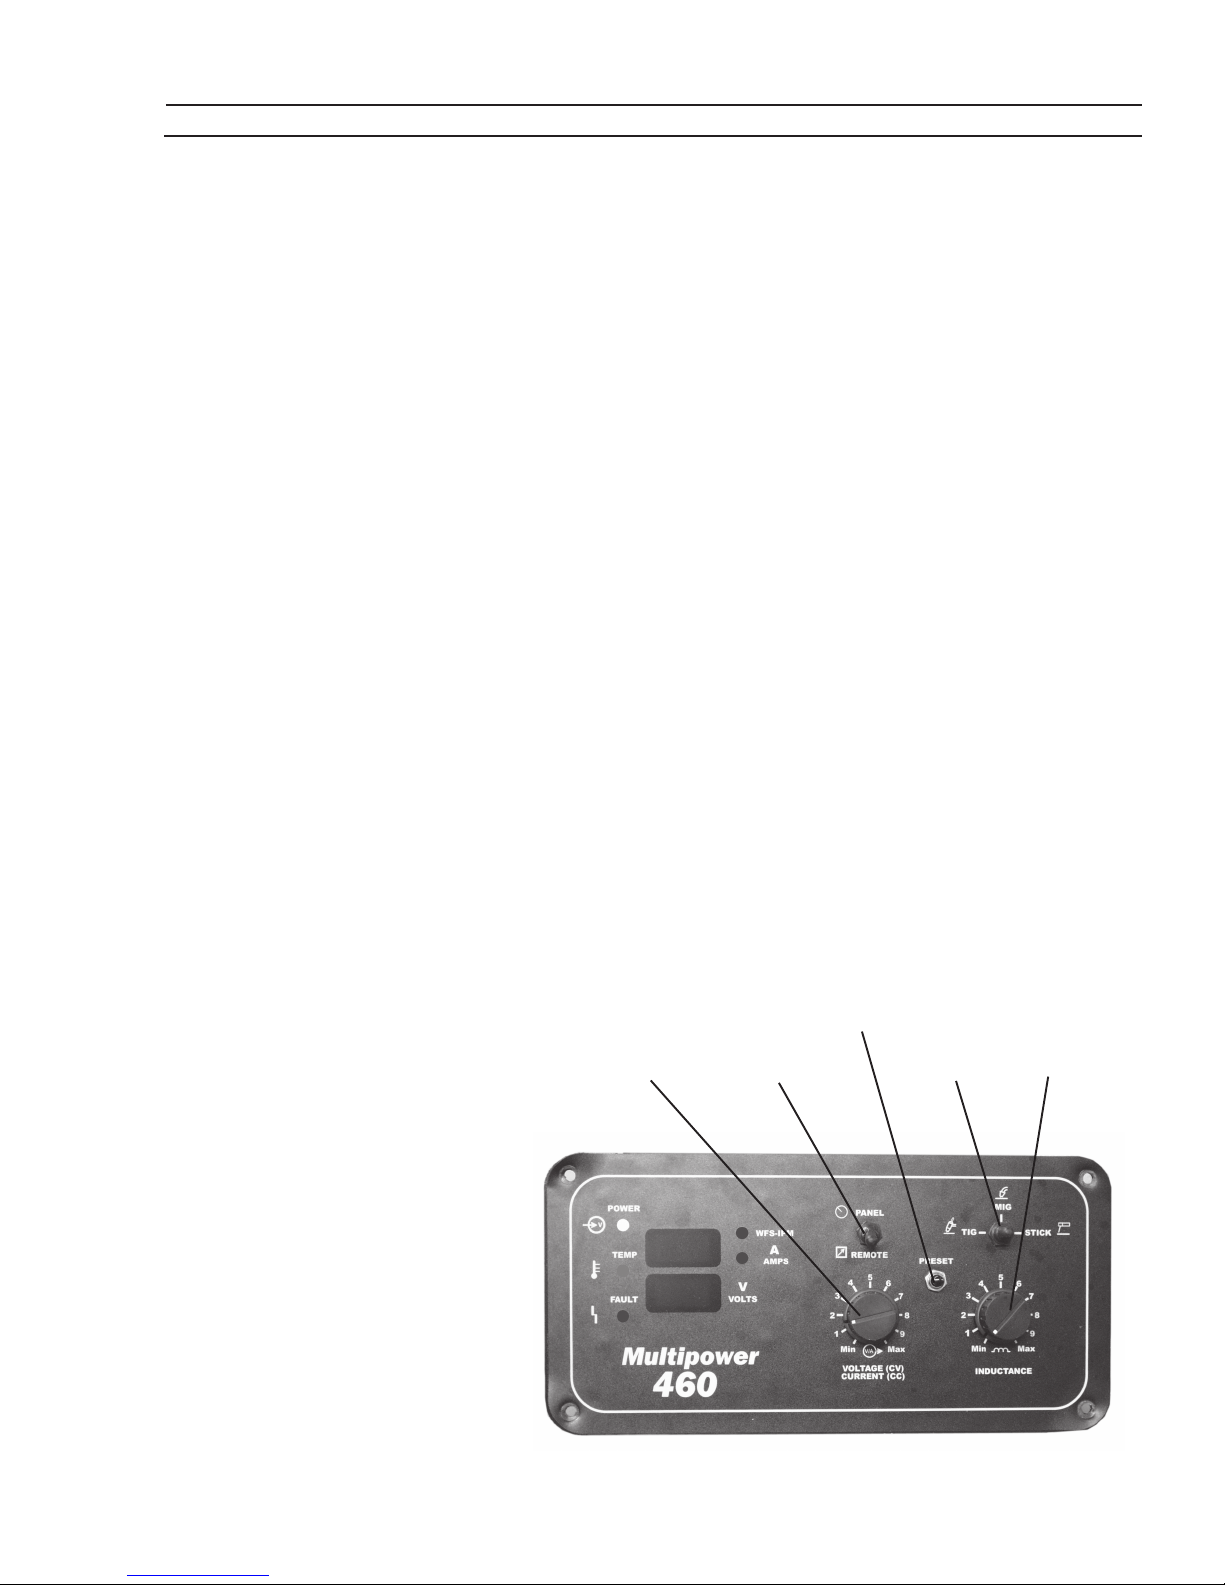
(Refer to Figure 2-3 and 2-4)
1. FAULT LAMP
The fault lamp is configured for future use and is not currently activated.
2. TEMPERATURE LAMP
The TEMP lamp illuminates if an over temperature condition occurs within
the MultiPower 460 power source. This condition may be caused by
excessive duty cycle or over-current conditions. When an over temperature
condition occurs, the welding output is turned off and the unit must be
allowed to cool. The machine will automatically reset when the temperature
falls to a safe level.
3. PROCESS SELECTOR SWITCH
The three position process selector switch is located in the upper right-hand
corner of the control panel. The process selector switch position provides
the visual indication of which weld process (Mig, Tig or stick) has been
selected.
4. DIGITAL DISPLAY/METERS (WFS, AMPS & VOLTS)
The digital displays located on the left side of the control panel are
multifunctional depending on the welding process being used. The top
display reads wire feed speed in inches per minute in the MIG PRESET
mode and welding current (amps) in the TIG and STICK PRESET mode.
During welding both displays indicate average welding current and average
welding voltage.
Temperature
Lamp
Fault
Lamp
Digital Meters
Amps/Volts/WFS
Power “ON”
Lamp
Figure 2-3. Standard Control Panel
WFS - IPM
Lamp
Amps
Lamp
12
Page 13
DESCRIPTIONSECTION 2
When using a DuraDrive 4-30 or DuraDrive 4-48 Wire Feeder, the wire feed
speed is displayed in inches per minute (IPM) in the top display when the
PRESET button is pressed and the wire speed adjustment knob on the wire
feeder is rotated. The WFS LED beside the top display meter will light when
the display is showing wire feed speed.
5. VOLTAGE/CURRENT TRIM
The arc voltage is controlled with this knob when the WELD PROCESS
selector switch is in the MIG position. The Mig arc voltage can be preset
by pressing the PRESET button and reading the arc volts in the bottom
digital display while rotating this knob.
The arc current is controlled with this knob when the WELD PROCESS
SWITCH is in the TIG or STICK position. The welding current can be preset
in amperes by pressing the PRESET button and reading the current (amps)
in the top digital display while rotating this knob. The average weld current
will be displayed during welding.
A DuraDrive Wire Feeder is required to
NOTE:
preset wire feed speed.
6. PANEL/REMOTE SWITCH
With this switch in the PANEL position, output voltage in the CV mode and
the output current in the CC mode are controlled by adjusting the VOLTAGE/
CURRENT/TRIM knob on the power source control panel to the desired
output. In the REMOTE position, output is controlled using a remote control
device such as a wire feeder, hand control or foot control.
7. INDUCTANCE TRIM
This control is used only in the MIG process mode and is deactivated in the
TIG and STICK modes. Inductance is used to optimize short circuiting arc
performance by changing the current rise and fall time of each short circuit.
This results in improved spatter control, weld bead wetting and arc stability.
The short circuiting Mig arc performance will change from a high short circuit
frequency, fast reacting arc, to a lower short circuit frequency, soft and less
spattering arc as the dial is turned clockwise. The optimized arc performance
will vary depending on shielding gas, wire type and wire diameter. The
operator can adjust this control to optimize welding characteristics.
Preset
Button
Current
Voltage
Panel/Remote
Weld Process
Switch
Inductance
Figure 2-4. Standard Control Panel
13
Page 14
DESCRIPTIONSECTION 2
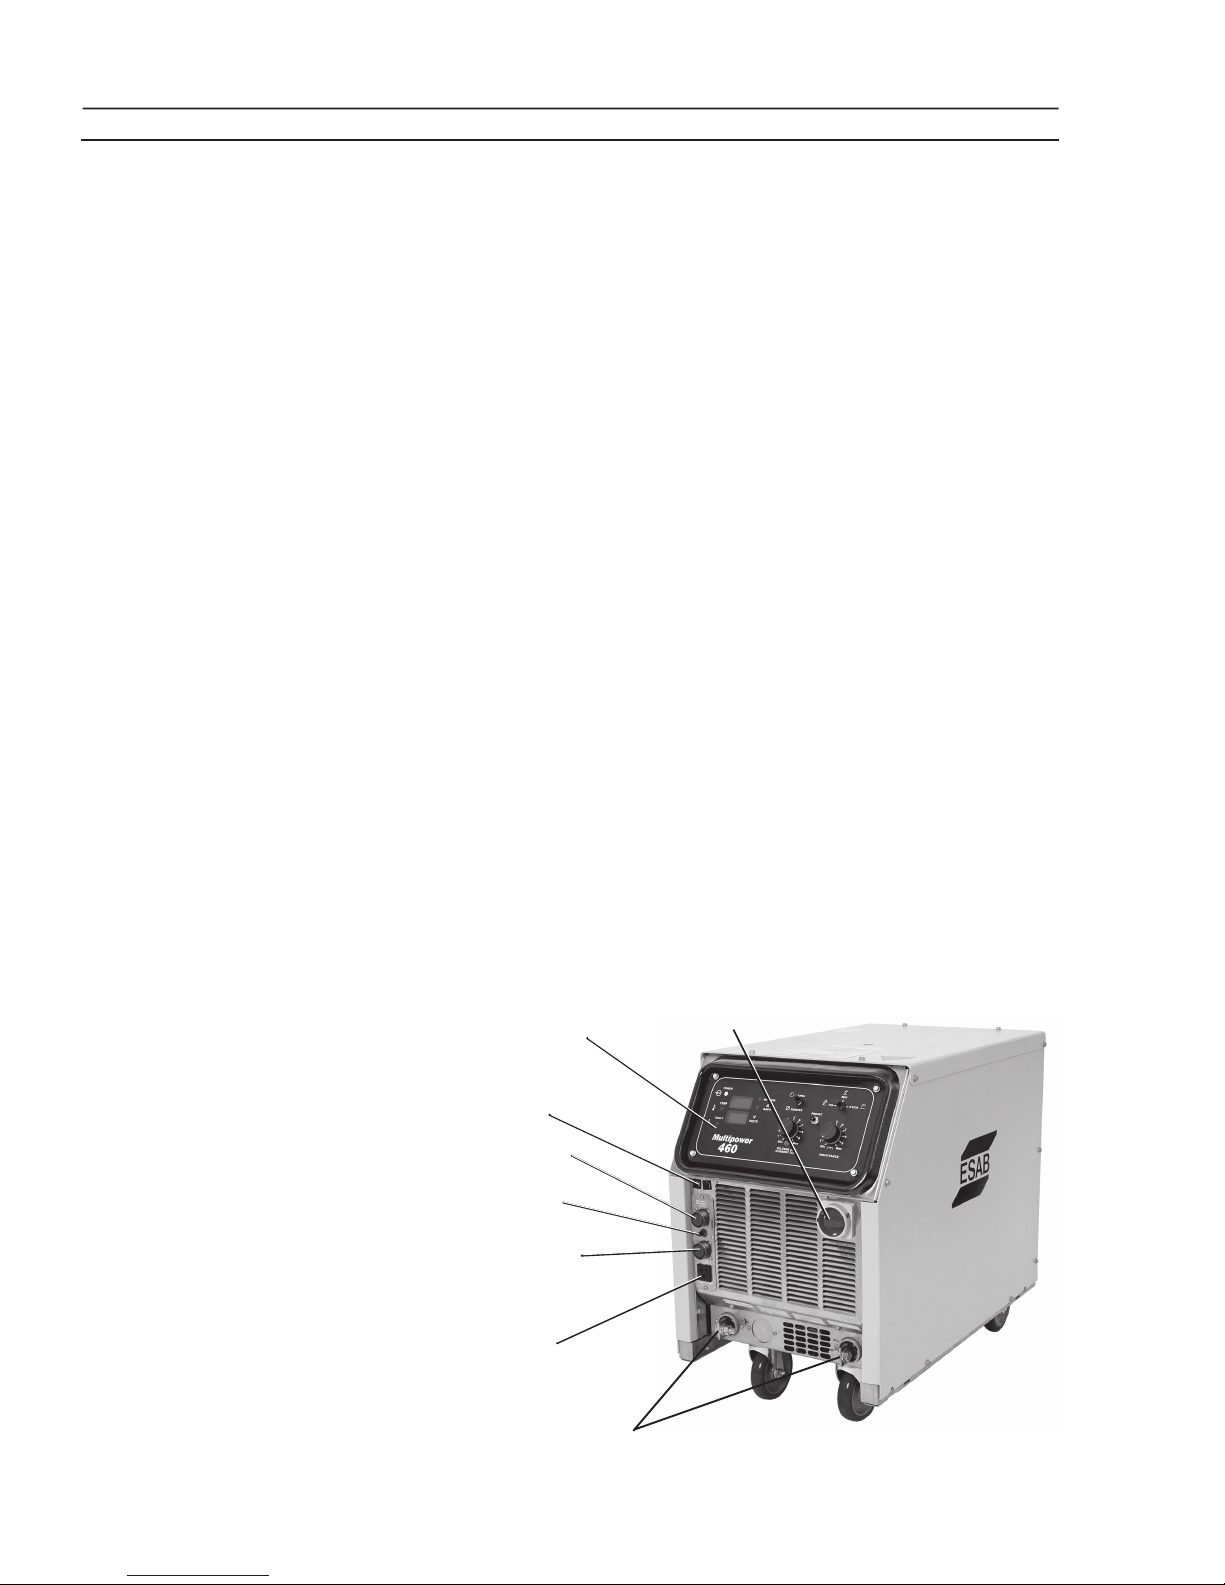
D. POWER SOURCE FRONT PANEL DESCRIPTION
(Refer to Figure 2-5)
1. POWER ON/OFF SWITCH & LAMP
The main power switch is located on the right front panel of the power source.
This switch energizes the main transformer, control circuitry and illuminates
the Power “ON” lamp.
2. WIRE FEEDER CONTROL RECEPTACLE
This 19-pin receptacle (J1) accepts the control cable from the wire feeder
and handles all the control signals needed to operate a 42 Vac wire feeder.
3. REMOTE CONTROL RECEPTACLE
This receptacle (J2) is provided for an optional 14-pin control cable from the
optional remote pendant, Tig torch control or foot control . This receptacle
is operative only if the PANEL/REMOTE switch on the power source front
panel is in the "REMOTE" position.
4. CONTACTOR "ON/OFF" SWITCH
This switch provides manual control of the welding contactor when the
PROCESS switch on the control panel is in the MIG position (CV welding).
An example of when to use this switch is when CV carbon arc gouging is
needed or an "Off the Arc" wire feeder with secondary contactor is operated
in the CV mode.
5. AUXILIARY 115 VAC RECPTACLE
A 115 Vac receptacle is provided to supply power to accessories such as
a water cooler, heated CO
regulator, or small hand tools. The receptacle
2
is rated 115 Vac / 10 amps with a floating neutral.
6. 42VAC AND 115 VAC CIRCUIT BREAKER (CB1 & CB2)
These resetable 10 amp circuit breakers (CB1 & CB2) protect the 42 volt wire
feeder/control and 115 volt auxiliary receptacle circuitry against over
current. (Table 7-1 provides troubleshooting information).
Main Power
Control Panel
On/Off Switch
Circuit Breakers
CB1 & 2
Wire Feeder
Connector
Contactor On/Off
Switch
Remote Pendant
Connection
115 Vac
10 Amps
Receptacle
Connections
Output
Figure 2-5. MultiPower 460
14
Page 15
SECTION 3
OPTIONAL EQUIPMENT AND ACCESSORIES
III. OPTIONAL ACCESSORIES
When using the MP-460 Pulse, the
NOTE
STANDARD/PULSE switch must be in
the STANDARD position for proportional
current control using a TIG remote cur-
rent device (FC-5B or TC-2B).
NOTE
The FC-5B foot control or TC-2B hand
control must be used with the MP-460 for
remote current Tig current control.
NOTE
If a Foot Control or Remote Hand Control
is used for continuous current control,
place the PANEL/REMOTE switch in the
PANEL POSITION and set the Panel Current knob to the maximum desired weld
current. The remote device will then control the current between minimum and the
maximum setting preset (proportional
current control). Maximum Tig weld current is 525 amps.
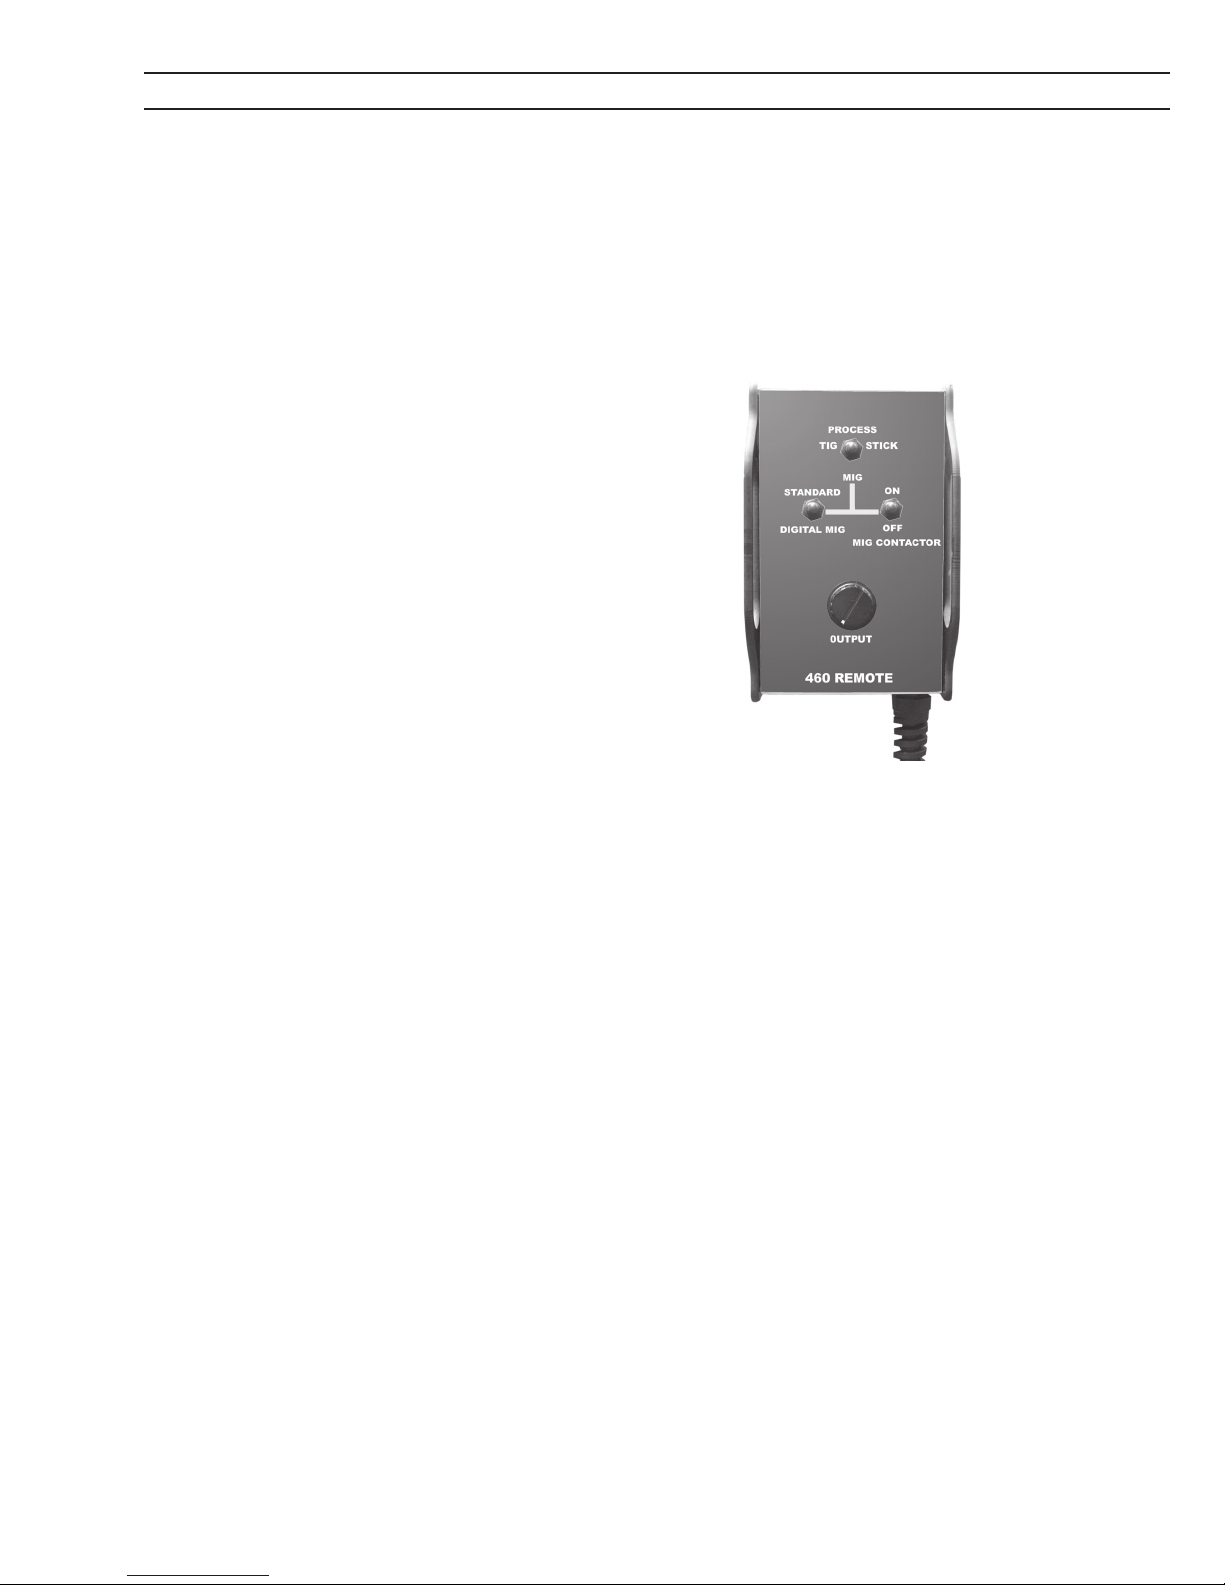
A. REMOTE HAND CONTROL (PN - 0558002871)
This pendant (Figure 2-2) provides remote output control and a contactor
closure switch to close the contactor making the output terminals “hot”. The
PANEL/REMOTE switch on the MultiPower 460 control panel must be placed
in the REMOTE position when using this accessory. The pendant has the
capability to change weld processes as well as adapt to digital and analog wire
feeders.
Figure 2-2. Remote Control Pendant
If the MP-460 PANEL/REMOTE switch is
NOTE
left in the REMOTE position when Tig
welding while using a remote current
control device, the current range will be
full scale or 10 to 400 Amps. Limiting
the the Maximum weld current on the
MP-460 front panel is defeated.
NOTE
When using a DuraDrive wire feeder
(or any wire feeder with Remote
Voltage control from the feeder front
panel) connected simultaneously with a
remote current control Tig device (FC5B or TC-2B), proportional control of
the TIG remote current will be controlled
by the position of the feeder voltage
control knob when the PANEL/REMOTE
switch is in the REMOTE position.
When in the PANEL position the
maximum current of the remote device
is controlled by the MP-460 front panel
current control preset.
TIG REMOTE CONTROLS
The following Remote controls are available for the Tig welding:
FC-5B EHD Foot Control 33841
FC-5B Foot Control 33838
TC-2B Torch Mount Control 33839
TC-3A Torch Mount On/Off only:
(HW-9, 17, 20, 20A & 24) 35783
(HW-18 & 26R) 36680
B. TR-29 TRUCK KIT (PN - 37924)
This truck kit provides complete mobility of the power source. The kit consists
of front castors, rear cylinder rack and wheels, gas cylinder bracket, cylinder
chain, and pull handle.
C. SWIVEL MOUNT KIT (PN - 36172)
This kit allows the wire feeder to be placed on an insulated swivel post on top
of the power source. The feeder can freely rotate, relieving potential wire feed
problems caused by sharp bends in the gun cable while, at the same time,
increasing the radius of the working area.
D. PULSE MIG UPGRADE KIT (PN - 0558002671)
This kit adds pulse gas metal arc welding to the MultiPower 460 and includes
and new control front panel.
15
Page 16
SECTION 4
For lifting purposes and for keeping dust, moisture, and other foreign material from entering the
power source, the lifting eyebolt
must be fully tightened with a tool.
Do not use filters on this unit as they
would restrict the volume of intake
air required for proper cooling. Output ratings on this unit are based on
an unobstructed supply of cooling
air drawn over its internal components. Warranty is void if any type of
filtering device is used.
INSTALLATION
IV. INSTALLATION
A. LOCATION
A proper installation site is necessary for the power source to provide
dependable service. A proper installation site permits freedom of air movement
through the unit while minimizing exposure to dust, dirt, moisture, and
corrosive vapors. A minimum of 18 inches (46 cm) is required between the side
and rear panels of the power source and the nearest obstruction.
The selected site should also allow easy removal of the power source outer
enclosure for maintenance. See Table 2-1 for overall dimensions of the unit.
B. RECEIVING, UNPACKING AND PLACEMENT
When requesting information concerning this equipment, it is essential that
Item number, Serial number and Model number of the equipment be supplied.
1. Upon receipt, remove all packing material and carefully inspect for any
damage that may have occurred during shipment. Any claims for loss
or damage that may have occurred in transit must be filed by the
purchaser with the carrier. A copy of the bill of lading and freight bill
will be furnished by the carrier on request.
2. Remove the power source from the container. Remove all packing
materials. Check the container for any loose parts.
3. Check air passages at front and rear of cabinet, making sure that
packing material has not obstructed air flow through the power source.
4. Install the lifting bolt furnished with the power sources into the top of
the unit.
5. After selecting an installation site, place the power source in the
desired location. The unit may be lifted either by using the lifting bolt
or by forklift truck. If a forklift is used for lifting the unit, be sure that
the lift forks are long enough to extend completely under the base.
C. PRIMARY (INPUT) ELECTRICAL CONNECTION
This power source is a three-phase unit and must be connected to a threephase power supply. It is recommended that the unit be operated on a
dedicated circuit to prevent impairment of performance due to an overloaded
circuit.
*Sized per National Code for 80 °C rated copper conductors @ 30 °C ambient. Not more than three
conductors in raceway or cable. Local codes should be followed if they specify sizes other than those
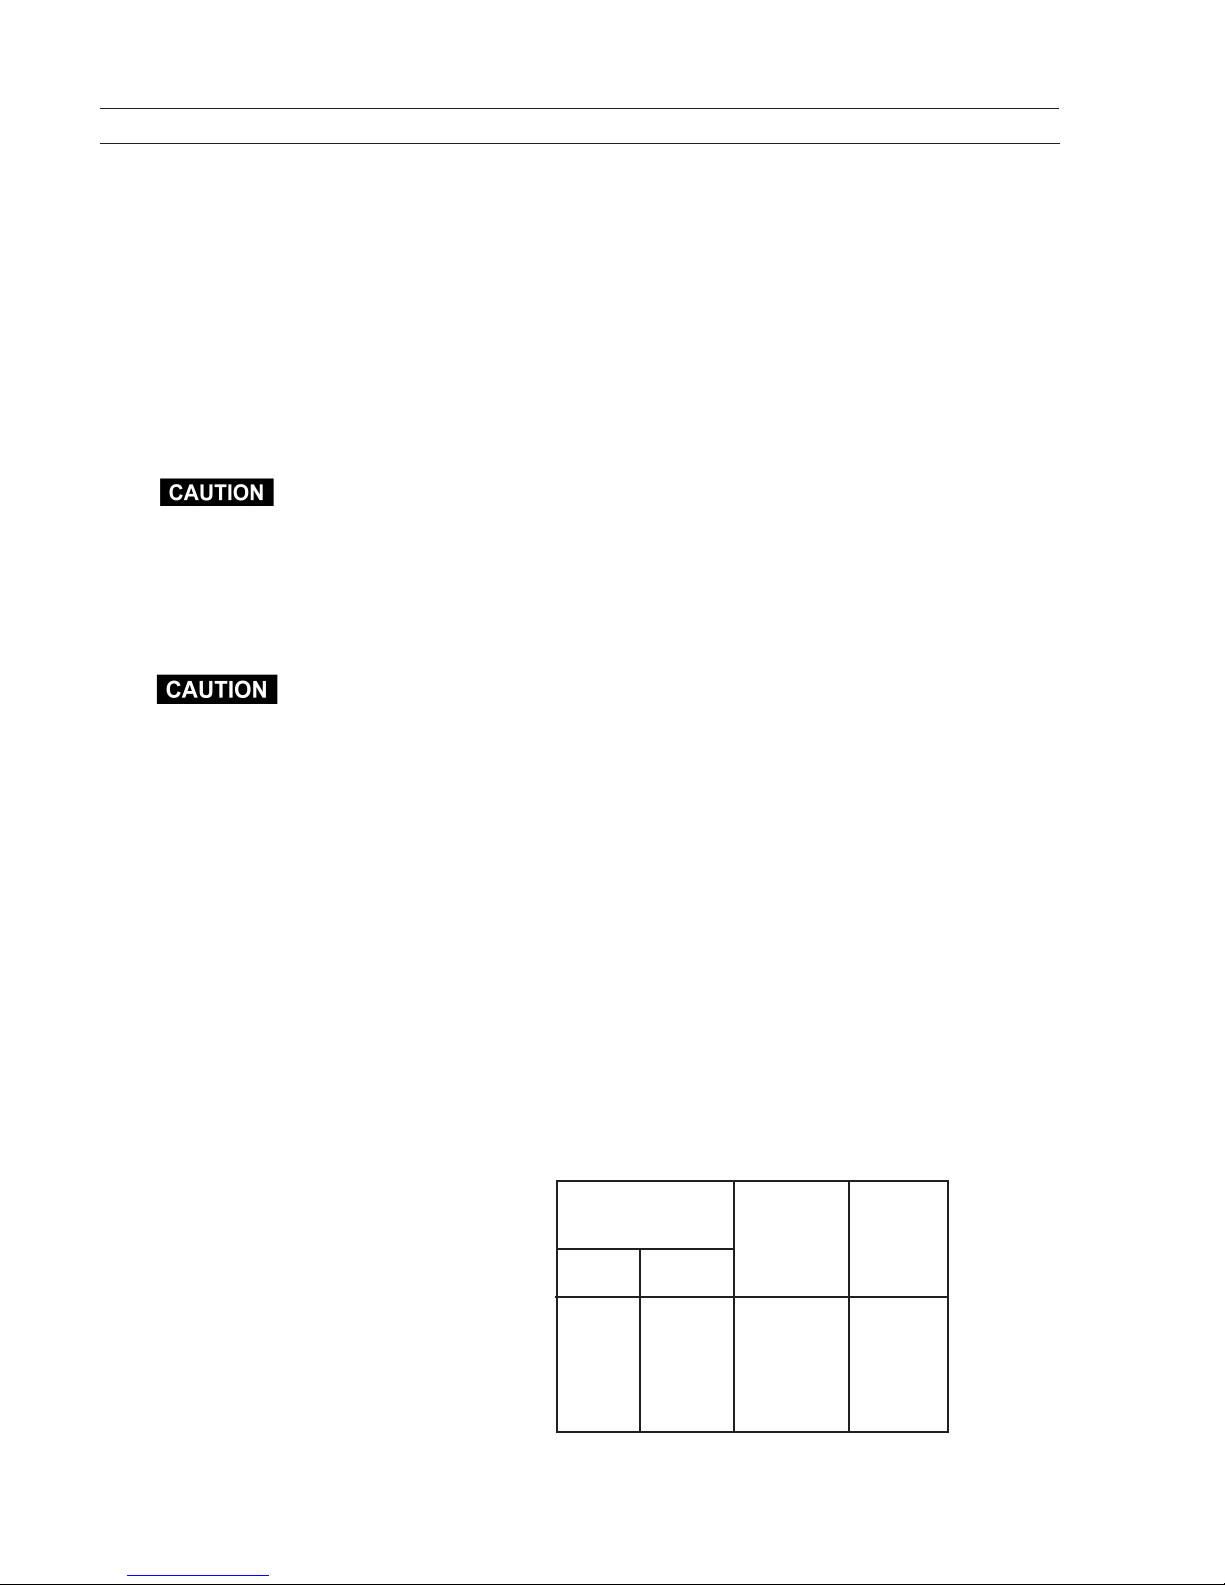
Table 4-1. Recommended Sizes for Input
Conductors and Line Fuses
Rate d Input
@ 100% Duty Cycle
Volts Amps
220
230
400
460
575
16
68
66
37
33
26
listed above.
Inp u t &
GND
Conductor*
CU/AWG
No. 6
No. 6
No. 8
No. 8
No. 1 0
Fuse
Size
Amps
100
100
60
60
50
Page 17
SECTION 4
INSTALLATION
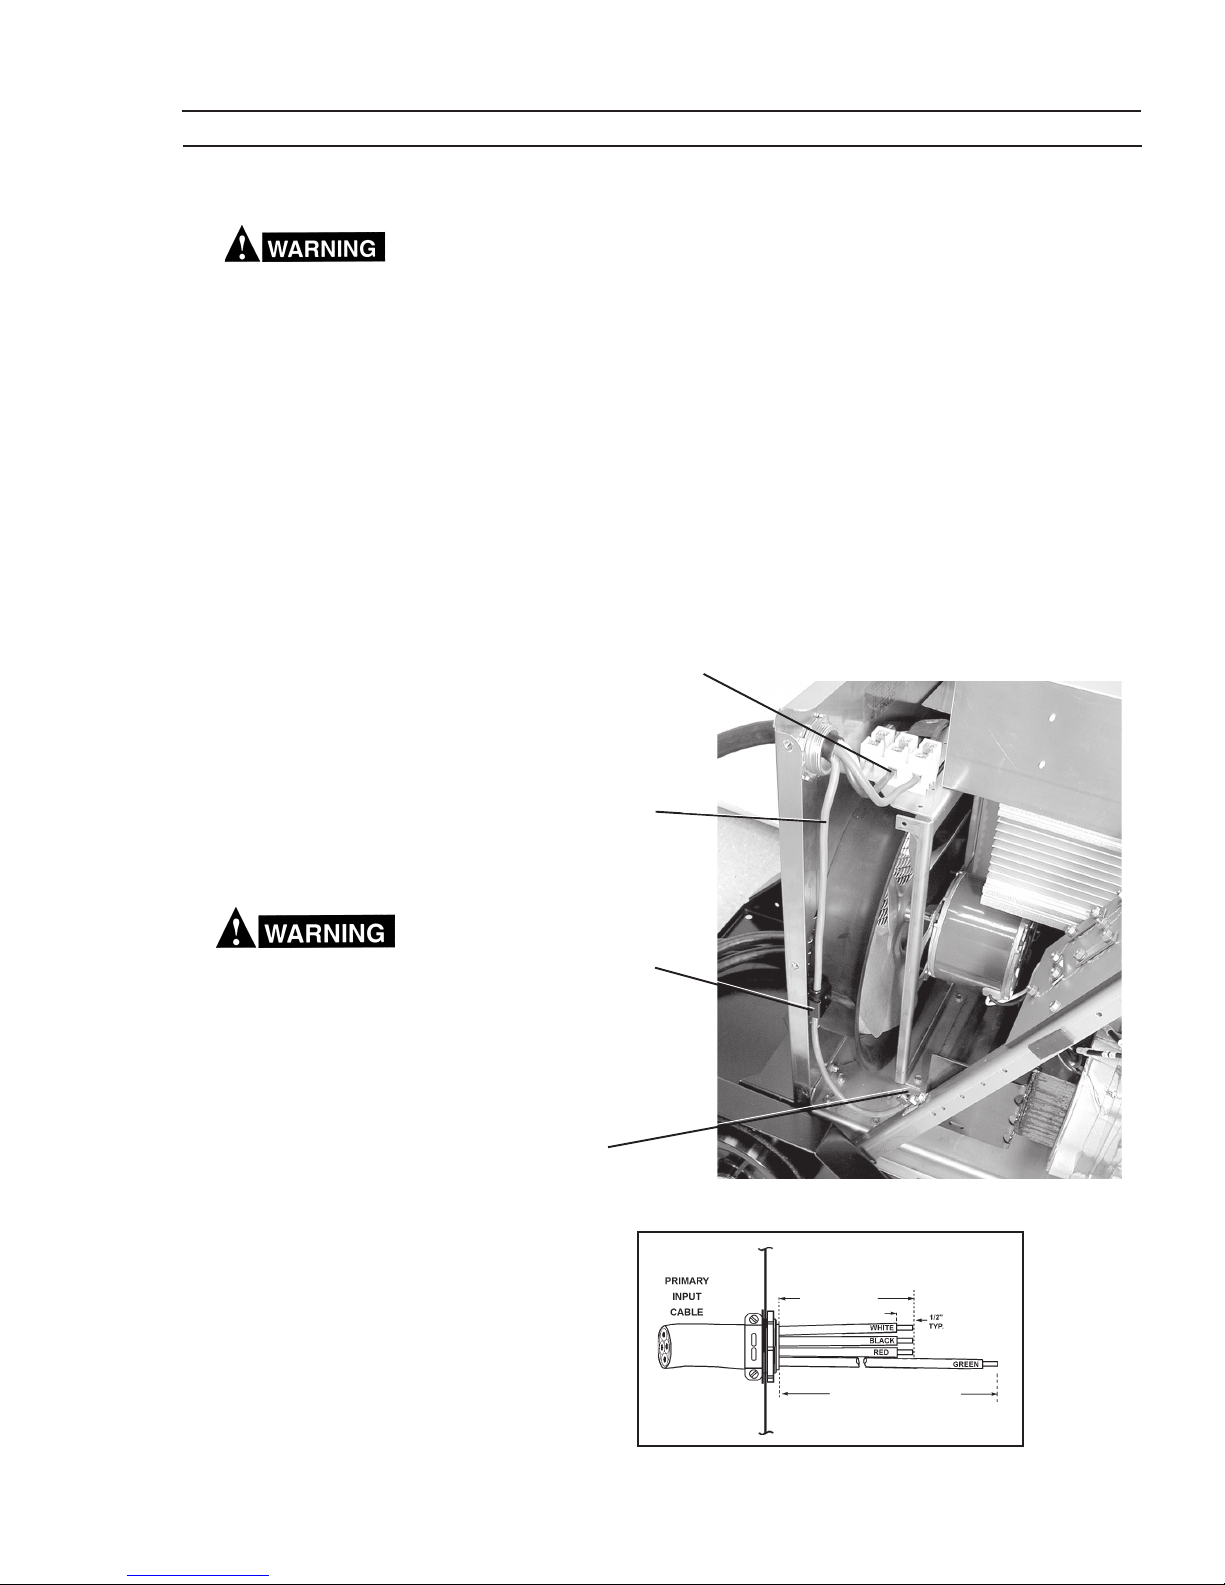
1. The primary power leads must be insulated copper conductors. Three
power leads and one ground wire are required. Either rubber covered
cable or conduit (flexible or solid) may be used. Table 4-1 provides
recommended input conductors and line fuse sizes.
ELECTRIC SHOCK CAN KILL! Before
making electrical input connections
to the power source, "Machinery
Lockout Procedures" should be employed. If the connections are to be
made from a line disconnect switch,
place the switch in the off position
and padlock it to prevent inadvertent
tripping. If the connection is made
from a fuse box, remove the corresponding fuses and padlock the box
cover. If it is not possible to use
padlocks, attach a red tag to the line
disconnect switch (or fuse box) warning others that the circuit is being
worked on.
2. Remove the top cover. Identify primary power input connection block,
chassis ground lug on the fan shroud frame, and primary input terminal
board. Refer to Figures 4-1, 4-2.and 4-3.
3. When using the provided strain relief, refer to Figure4-2 for proper cable
strip lengths. It is important to follow the cable strip guide to ensure
that if the primary input cable is ever pulled from the strain relief, the
input conductors will be pulled from the Terminal Block before the
ground lead is pulled from the ground lug. Once stripped, thread the
input and ground conductors through the large strain-relief in the rear
panel of the power source. Connect the ground wire to the terminal lug
located on the fan shroud frame. Connect the primary power leads to
terminals L1, L2, and L3 on the input power block. Secure the strain
relief on the input cable.
4. Check all connections for proper tightness. Ensure all connections
are correct and well-insulated.
TB-3
L1, L2, L3
Connection
Primary Cable
(Supplied by Customer)
The chassis must be connected to an
approved electrical ground. Failure
to do so may result in electrical shock,
severe burns or death.
Ground Fault
Switch & Bracket
Ground
Connection
Figure 4-1 Primary Power Leads L1,L2, L3 & Ground
Figure 4-2
17
(3) PRIMARY
INPUT
CONDUCTORS
24"
Green
Recommended Cable Strip Lengths
Page 18
INSTALLATIONSECTION 4
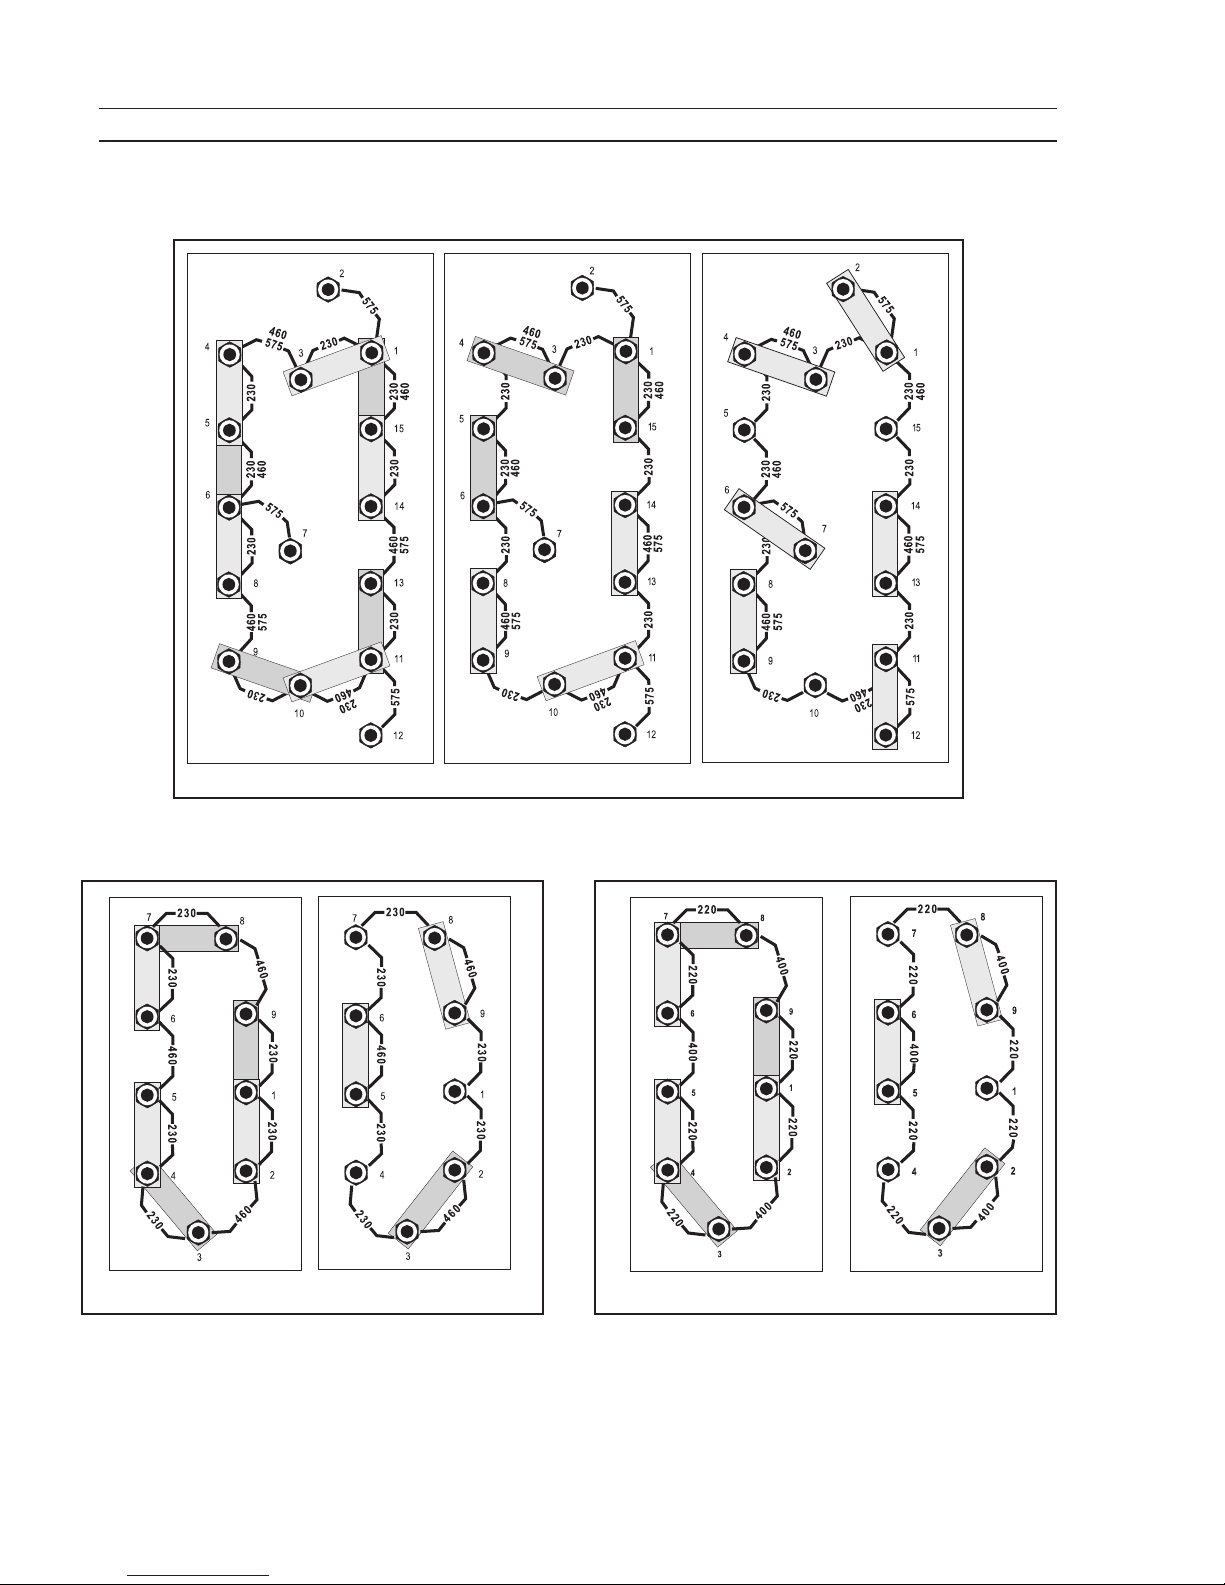
230 Vac Input 460 Vac Input 575 V ac Input
Input T erminal Board Configuration for 230/460/575 Model
230 Vac Input
Input T erminal Board Configuration 230/460 Model
460 Vac Input
*
*
*
220 Vac Input
Input Terminal Board Configuration 220/400 Model
400 Vac Input
Unit is factory shipped in the 575 Vac configuration
Figure 4-3 Input Terminal Board
18
Page 19
SECTION 4
Check the voltage links for proper
voltage on the Input Terminal board
before applying primary power.
Before making any connections to
the power source output terminals
make sure that all primary input power
to the machine is off.
INSTALLATION
5. Figure 4-3 illustrates the input voltage terminal board and the input voltage
link connections. The particular voltages from which this power source may be
operated are stated on the rating plate. The voltage links were factory set for
highest voltage stated on the rating plate. If the power source is to be operated
on another stated input voltage, the links must be reset for that particular input
voltage. Always verify the input voltage and check the link arrangement
regardless of factory setting. The voltage links are set up by reconfiguring the
copper link bars to the voltage designations for the desired voltage.
D. OUTPUT WELDING CONNECTIONS
(SECONDARY)
The output connections are located on the front panel (Figure 2-5). The positive
connection is located at the bottom left corner and the negative connection is
located at the bottom right corner. Table 2-2 provides the recommended
secondary cable output sizes.
1. CONNECTIONS FROM THE WIRE FEEDER
The wire feeder control cable connects to the 19 pin J1 receptacle on the lower
front left of the MultiPower 460. The secondary output cable connects (in most
cases) between the positive output lug of the MultiPower 460 and the power
connection block of the wire feeder. See the wire feeder installation instructions for other connections such as shield gas, water, remote controls, Mig
guns and wire feeder operation.
2. CONNECTIONS FOR STICK AND TIG WELDING
The Tig torch and stick electrode holder connect directly to the appropriate
MultiPower 460 output lugs on the lower front panel. The choice of the Positive
or Negative terminal depends on the welding process and electrode type being
used. In most cases the Tig torch will connect to the negative lug and work
cable will connect to the positive lug. The stick electrode holder usually
connects to the positive lug and the work cable to the negative lug.
Table 4-2. Output Cable Sizes (Secondary)
Total Length (Fee t ) of
Welding
Current
100
150
200
250
300
400
50 100 150 200 250
6
4
3
2
1
2/0
Cable in Weld Circuit*
4
3
1
1/0
2/0
3/0
3
1
1/0
2/0
3/0
4/0
1/0
2/0
3/0
4/0
4/0
2
1/0
2/0
3/0
4/0
4/0
2-2/0
500
* Total cable length includes work and electrode cables. Cable size is based on direct
current, insulated copper conductors, 100-percent duty cycle and a voltage drop of 4 or
less volts. The welding cable insulator must have a voltage rating that is high enough to
withstand the open circuit voltage of the power source.
3/0
3/0
4/0
2-2/0
2-3/0
19
Page 20
INSTALLATIONSECTION 4
20
Page 21
SECTION 5 OPERATION
V. OPERATION
A. WIRE FEEDER COMPATIBILITY
Never operate the power source
with the covers removed. In addition to the safety hazards, improper
cooling may cause damage to the
components. Keep side panels and
top closed when unit is energized.
Welding helmet, gloves, and other
personal protection should always
be worn when welding.
NOTE
Wire Feeders with 115VAC contactor control circuitry cannot be
connected to the MultiPower 460.
NOTE
The digital wire feed speed meter
on the MultiPower front panel reads
a maximum of 760 ipm. Some
wire feeders have speed ranges
that exceed this maximum limit of
the digital meter. Wire feed speeds
above 760 ipm will be displayed at
760 ipm.
NOTE
The digital volt meter on the MultiPower front panel reads a maximum of of approximately 75 Vdc
even if the OCV (Open Circuit Voltage) is higher. The MultiPower
460 has the following OCV"s:
STICK 75 to 80 Vdc
TIG - 38 to 42 Vdc
MIG - 11 to 44 Vdc
The MultiPower 460 Pulse power source can be used with several ESAB 42
volt wire feeders. The model wire feeder being used will determine the setup
method and operator interface. The position of the REMOTE/PANEL switch
determines the location of the voltage preset and TRIM locations. The wire feed
speed is always set from the wire feeder using the wire speed knob on the
feeder control panel. To see the preset wire feed speed, press the PRESET
button on the MultiPower 460 control panel. Use Table 5-1 to determine the
switch position of operator preference. In most Mig welding applications, the
switch will be in the REMOTE position and the wire feed speed and voltage will
be adjusted from the wire feed front panel.
Table 5-1. Wire Feeder Compatibility
MIG MODE SWITCH*
MIG STANDARD
(MultiPower 460)
Wire Feeder
Mig 4HD
DuraDrive 4-30
DuraDrive 4-48
Mig 2E
Mig 5XL
(Mongoose)
Mobile Ma ster IV
(Off the Arc)
Mini 8
(Off the Arc)
N/A - Not Available
* - Process switch MUST be in the MIG position.
** - See Sy nergic/NonSynergic description section for configuration information
(Applies to MultiPower 460 Pulse only)
Arc Trim Location
from:
Feeder X X Optional
Remote Pendant X X Optional
MP- 460 Panel X X Optional
Feeder X N/A
Remote Pendant X X Optional
MP- 460 Panel X X Optional
Feeder X N/A N/A X
Remote Pendant X N/A X
MP-460 Panel X N/A X
PANEL REMOTE Synergic
MIG PULSE
(Mul ti P ow e r 460 Pu l se)
Non-
Synergic**
B. DIGITAL DISPLAY METERS
The digital displays located on the left side of the control panel are multifunctional depending on the welding process being used. The MultiPower 460
digital display meters permit preset of the wire feed speed on wire feeders
without digital displays. A Mig 2E, 4HD or DuraDrive 4-30 or 4-48 will not need
digital meters to preset the wire feed speed. The wire feed speed can be
displayed on the MultiPower 460 panel meter.
C. MIG WELDING
In the MIG process mode, the digital displays will read preset wire feed speed
in inches per minute and preset arc volts when the PRESET button is pressed.
Once welding begins, the displays will show average welding current and volts
in the top and bottom display, respectively. The displays have a “HOLD” circuit
that retains the welding conditions. After welding stops, the display will
continue to show the last average welding current and voltage sampled for 10
seconds, then returns to “0”.
D. TIG and STICK WELDING
In the TIG and STICK process mode, you must depress and "HOLD" the
PRESET button while presetting the welding current in the top display.
Releasing the preset button causes the display to return to zero. Once welding
begins, the display will show average welding current and volts in the top and
bottom display, respectively. After welding stops, the current display will again
return to zero. There is no “HOLD” circuit for the display meters when using
the TIG and STICK process modes.
21
Page 22
SECTION 5 OPERATION
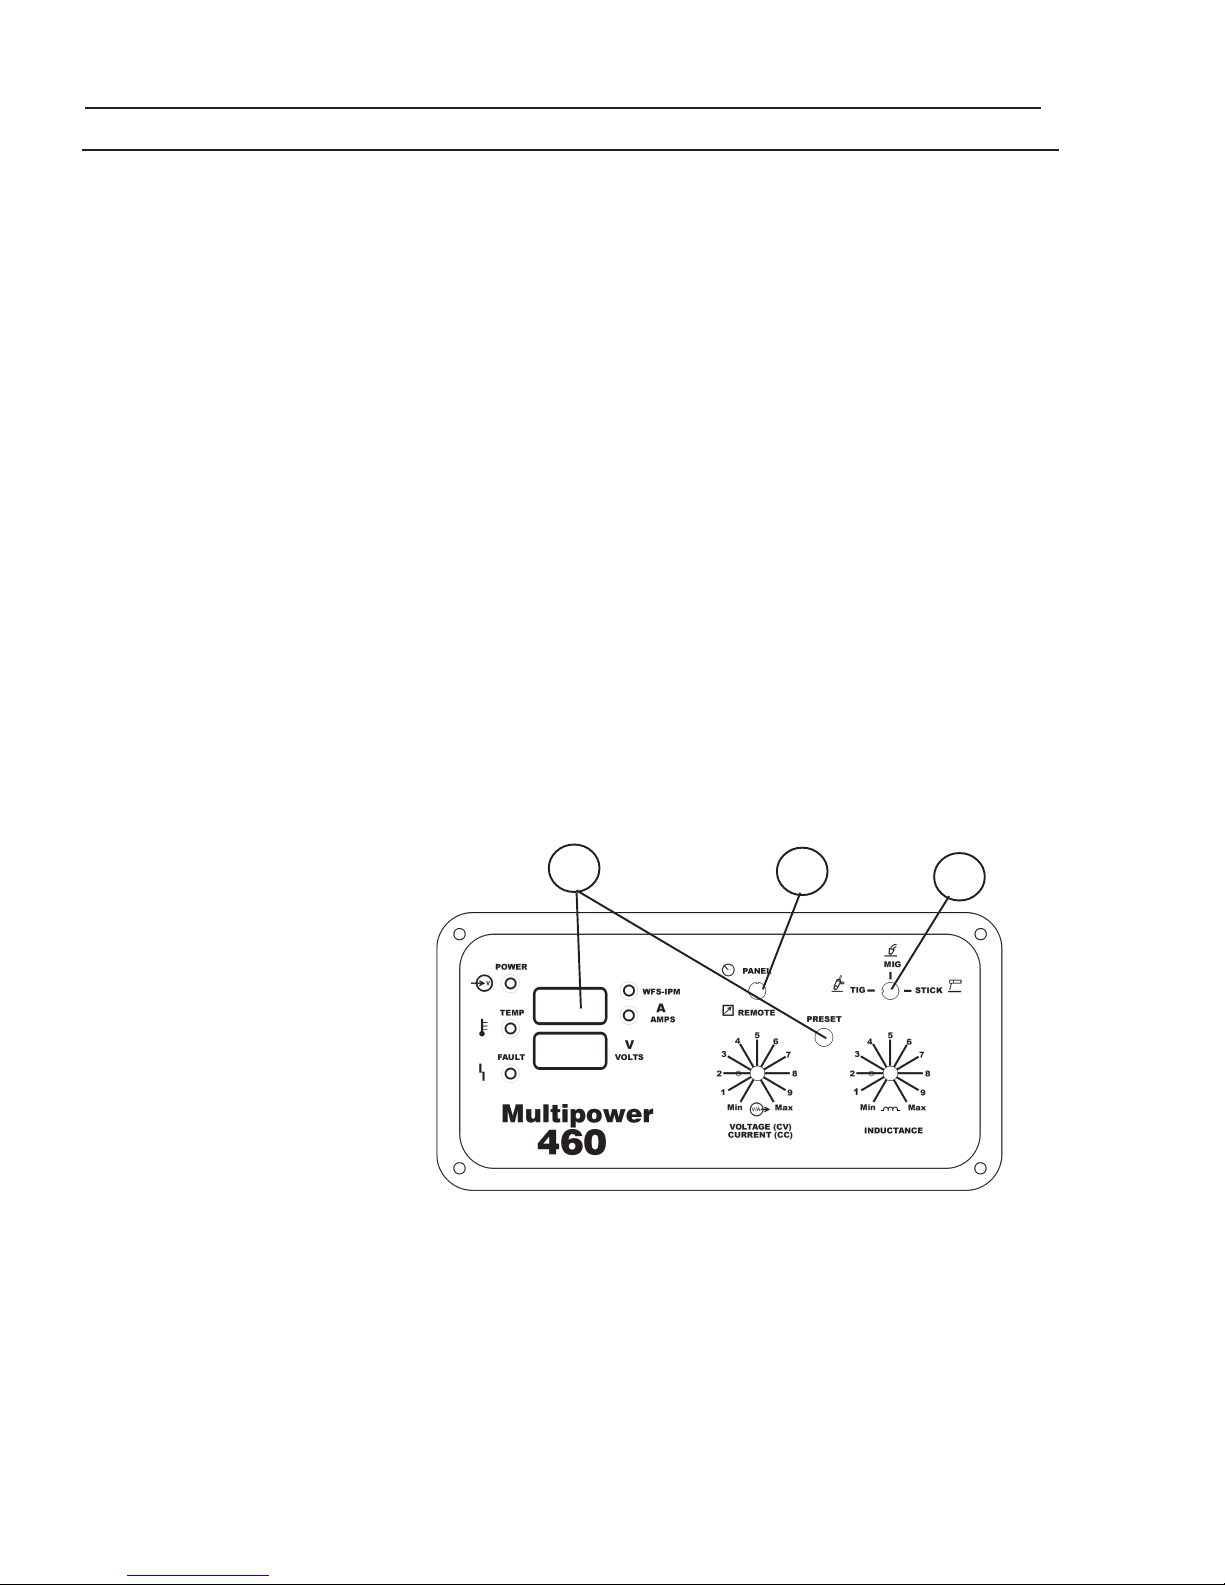
E. MIG WELDING PRESET PROCEDURE
When the PROCESS switch is placed in the MIG position, the MultiPower 460
is set for CV (constant voltage) welding. The power source will output open
circuit voltage (OCV) when the Mig Gun trigger is depressed. The following
procedure assumes the wire feed and voltage adjustments will be made from the
wire feeder front panel and wire and gas have been installed.
Step 1. Connect wire feeder to MultiPower 460 and set PANEL/REMOTE
switch to REMOTE position.
Step 2. Place the WELD PROCESS switch in the MIG (center) position.
NOTE
"OFF THE ARC" Wire Feeders
can use either MIG (CV) or STICK
(CC) Process Selection. Place
the contactor toggle switch on
the accesssory panel (see Figure 3-5) to the "ON" position.
Step 3. Press and release the PRESET button t hen turn the
control on the wire feeder to the desired speed shown on the top
digital display window of the MultiPower 460.
Step 4. Turn the VOLTAGE knob
voltage in the bottom digital display window of the MultiPower 460.
Step 5. Set the shielding gas flow rate to 35 cfh by activating the gas purge
switch on the wire feeder or pulling the gun trigger and turning the
adjustment knob on the Flowmeter .
Step 6. Connect the work cable to the part top be welded and pull the gun
trigger to start welding. Trim the wire speed and volts as needed for
the desired arc characteristics and weld quality .
3
on the wire feeder to the desired arc
1
wire speed
2
Figure 5+-1 Standard Mig Setup Procedure
22
Page 23
SECTION 5
OPERATION
F. TIG WELDING
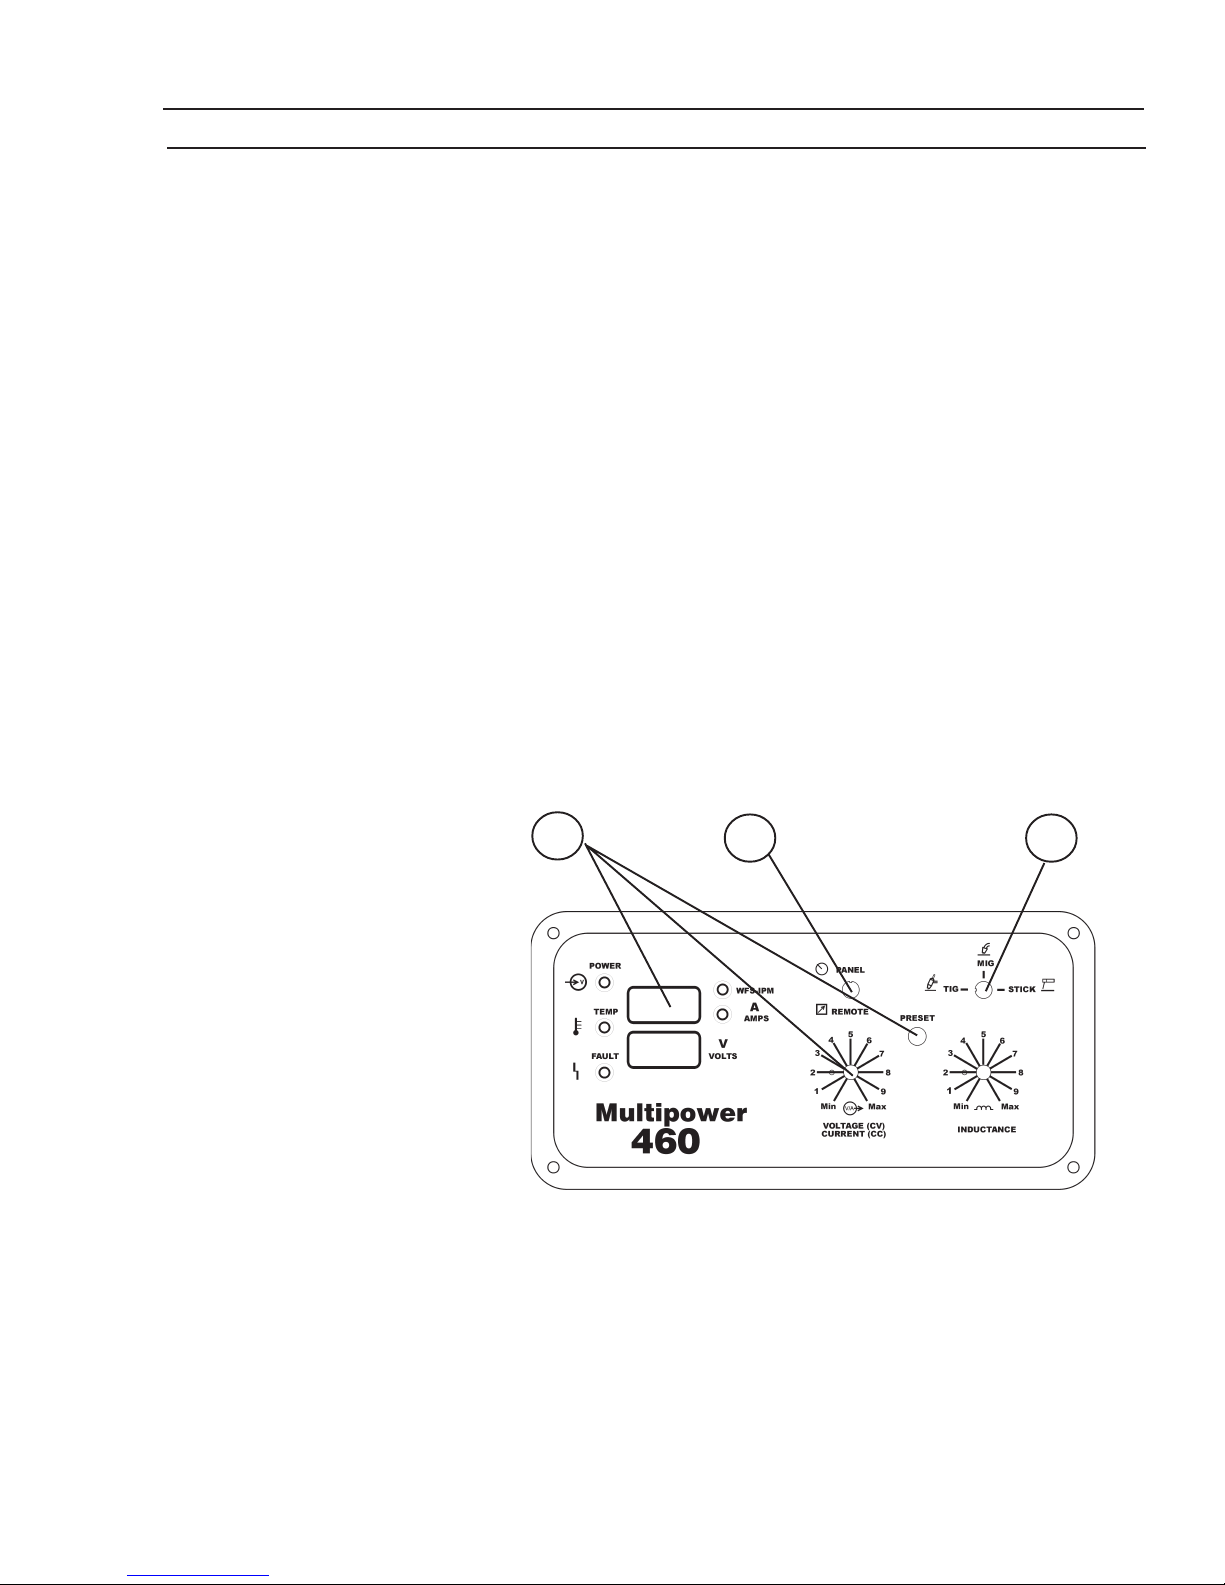
When the PROCESS switch is placed in the TIG position, the MultiPower 460
is automatically set for CC (constant current) welding using the ESAB Touch
TIG starting method. The voltage and current at the output lugs is maintained
at low values until the electrode is shorted to the workpiece.
Step 1. Be sure to set the polarity to DCEN (Electrode Negative) by connect-
ing the Tig torch to the negative terminal lug on the front of the power
source.
Step 2. Place the WELD PROCESS switch in the TIG position.
Step 3. Place the PANEL/REMOTE switch in the P ANEL position.
Step 4. While depressing the PRESET button, turn the VOLT AGE/CURRENT
knob to the desired weld current as displayed on the top digital dis-
play window.
Step 5. Set the shielding gas flow rate to 20 cfh by adjusting the control knob
on the flowmeter.
NOTE:
If a Foot Control or Remote Hand
Control is used for continuous current control, place the PANEL/
REMOTE switch in the REMOTE
POSITION and set the Panel
Curent knob to the maximum desired weld current. The remote
device will then control the current
between minimum and the maximum setting preset.
Step 6. Touch the tungsten electrode to the workpiece moment arily then lift
1/16" off the workpiece to establish the welding arc. Trim the weld
current as desired by turning the VOL T AGE/CURRENT knob.
4
Figure 5-2 Standard Tig Setup Procedure
23
23
Page 24
SECTION 5
OPERATION
G. STICK WELDING
When the WELD PROCESS switch is
moved to the TIG or STICK position, electrode becomes electrically “HOT”. Do not allow the electrode to contact ground potential
until you are ready to make a weld.
When the PROCESS switch is placed in the STICK position, the MultiPower
460 establishes open circuit voltage (OCV) and output power is immediately
available for welding. This means that the STICK electrode holder is “HOT”, and
an arc will strike when the electrode comes in contact with the workpiece or any
other object at ground potential.
Arc Force is automatically enabled when the WELD PROCESS switch is set
to the STICK position. The level of Arc Force is automatically adjusted by the
current preset being used.
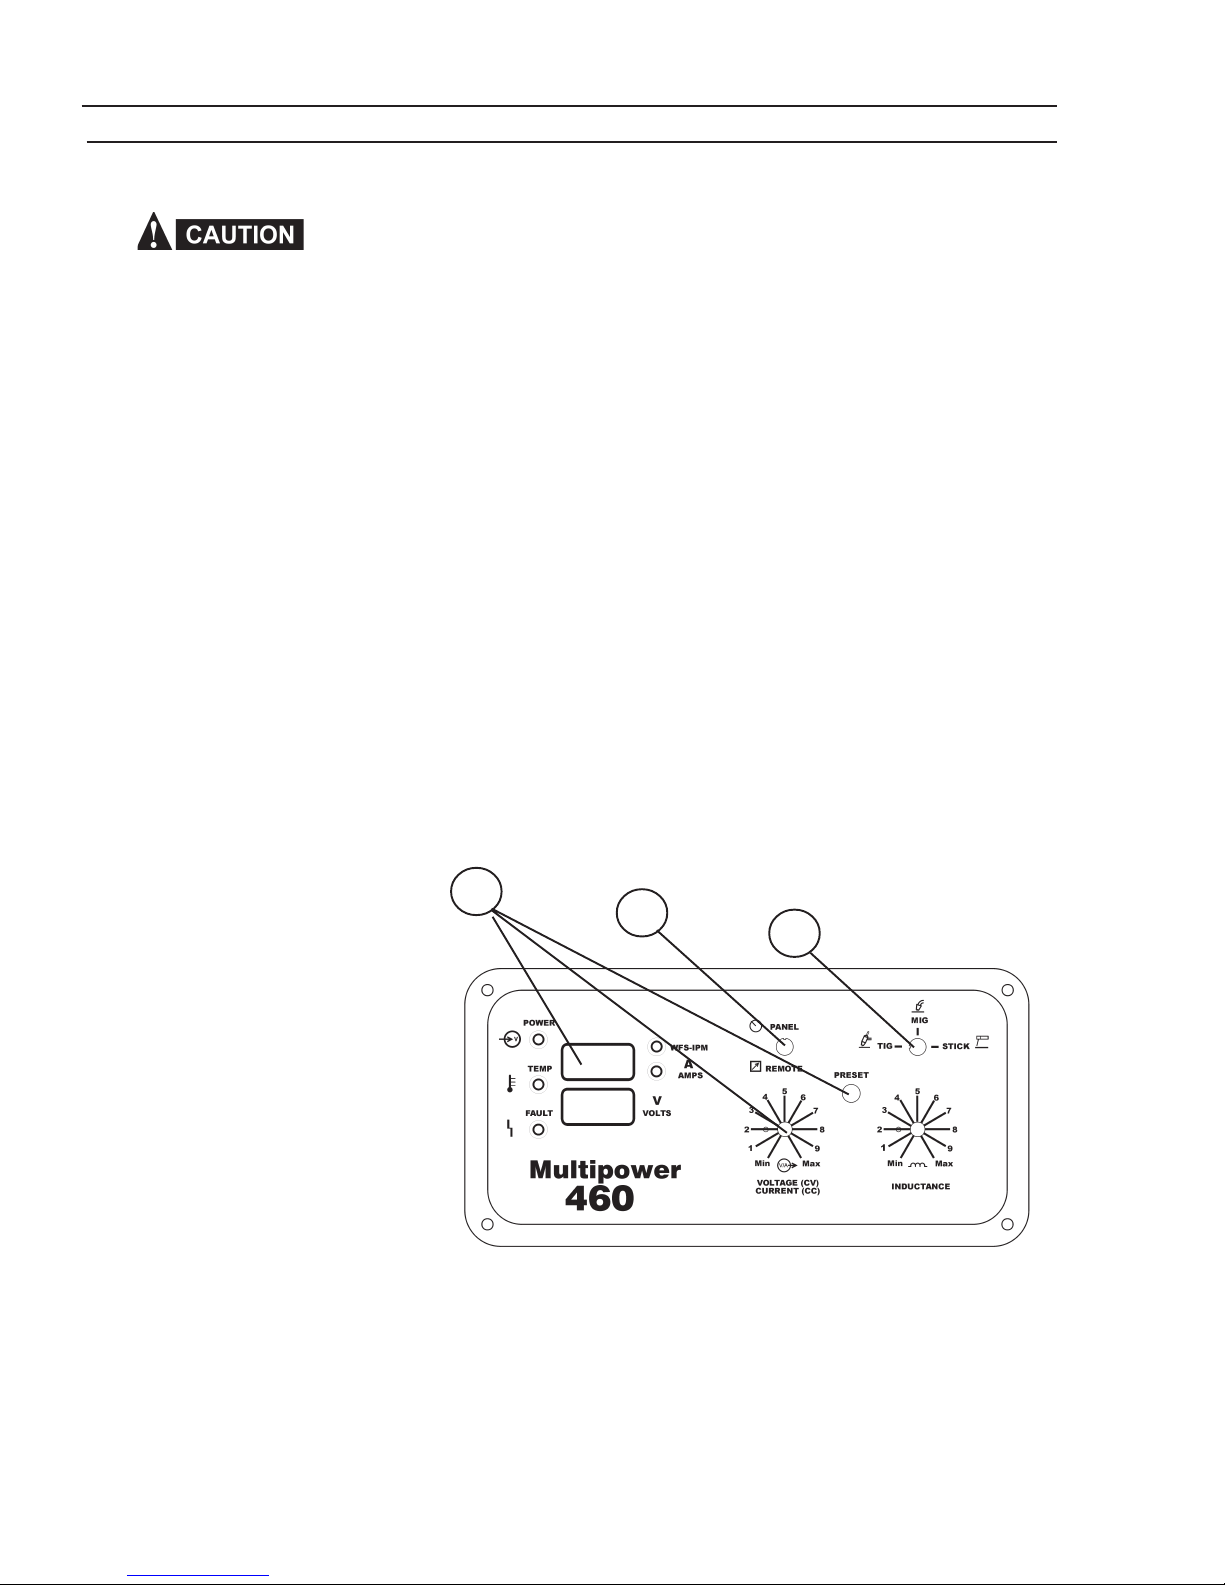
Step 1. Be sure to set the polarity to DCEP (Electrode Positive) by placing
the Electrode Holder cable in the Positive connection lug on the front
of the power source.
Step 2. Place the WELD PROCESS switch in the STICK position.
Step 3. Place the PANEL/REMOTE switch in the P ANEL position.
Step 4. While holding the PRESET button, turn the VOLTAGE/CURRENT
knob to the desired weld current in the top digital display window .
Step 5. Strike the electrode on the workpiece and start welding. Trim the
welding current as needed for the desired weld pool control.
4
3
2
Figure 5-3 Standard Stick Setup Procedure
24
Page 25
SECTION 5
OPERATION
H. AIR CARBON ARC GOUGING (CAC-A)
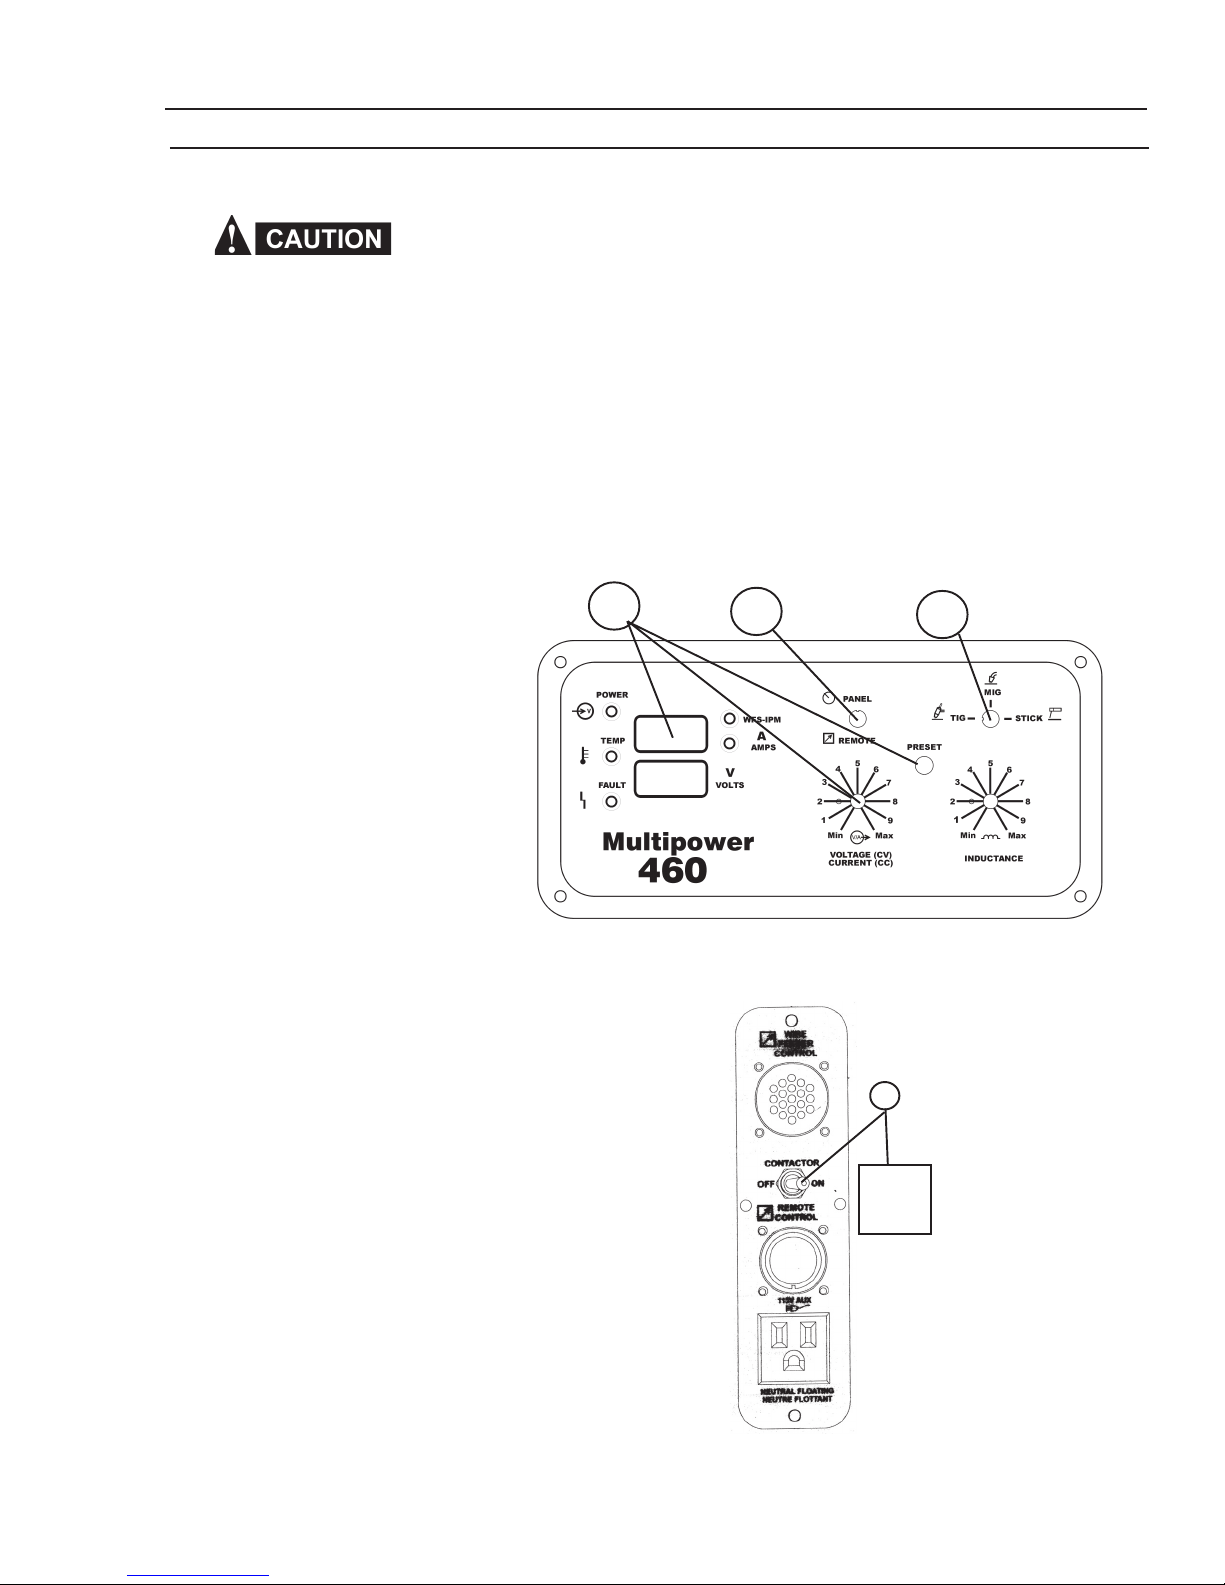
1. CONSTANT CURRENT and CONSTANT VOLTAGE GOUGING
When the WELD PROCESS switch is
moved to the TIG or STICK position,
electrode becomes electrically
“HOT”. Do not allow the electrode
to contact ground potential until
you are ready to make a weld.
Note: Due to the "Built-In" Arc Force
in the stick mode, the actual
current may be greater than
the preset value.
Step 1. Place the Output PANEL/REMOTE switch into PANEL position if
output current is regulated from the VOLTAGE/CURRENT knob on the
power source front panel, or in REMOTE position if output current is
regulated from the optional Hand Control.
Step 2. Place the Process Control switch in the STICK position.
Step 3. Press and hold the PRESET button and set the VOLTAGE/CUR-
RENT knob to gouging current.
Step 4. CV-Carbon Arc Gouging Only - Place the Process Switch in the
MIG position and the Contactor Toggle switch to the "ON" position.
See Figures 5-4 and 5-5.
Step 5. Turn the air on the gouging electrode holder "ON and start gouging
by touching or scratch starting the electrode.
3
1
2
Figure5-4 Standard Carbon Arc Setup Procedure
4
CV
Figure 5-5 Contact Switch for Carbon Arc Setup
25
Page 26
SECTION 6
MAINTENANCE
VI. CLEANING
If this power source does not operate
properly, stop work immediately and
investigate the cause of the malfunction. Maintenance work must be performed by an experienced person,
and electrical work by a trained electrician. Do not permit untrained persons to inspect, clean, or repair this
power source. Use only recommended replacement parts.
Be sure that the branch circuit or main
disconnect switch is off, or electrical
input fuses are removed, before attempting any inspection or work inside the power source. Placing the
power switch in the off position does
not remove all power from inside the
power source.
Periodically, remove the cover from the power source and blow accumulated
dust and dirt from the air passages and interior components by using clean low
pressure air. The frequency of cleaning required depends upon the environment
in which the power source is used.
It is imperative that all air passages be kept as clean as possible in order to
allow adequate air flow to provide proper cooling.
After cleaning with low pressure air, check for and tighten any loose hardware,
including all electrical connections. Check for frayed and/or cracked insulation
on all power cables and replace if necessary.
A. INSPECTION AND SERVICE
Keep the power source dry, free of oil and grease, and protected at all times
from damage by hot metal and sparks.
1. FAN MOTOR
Keep the fan motor free of accumulated dust and lint.
2. TRANSFORMER
Other than periodically cleaning the dust and dirt from the transformer, no
maintenance is required. Ensure that only clean, dry, low pressure air is
used.
Failure to replace worn or damaged
cables may result in a bare cable
touching a grounded object. The
resulting electrical arc may injure unprotected eyes and will present a
serious fire hazard. Body contact
with a bare cable, connector, or conductor may result in severe electrical
shock, causing serious burns or
death.
3. WIRE FEEDER CONTROL CIRCUITS
These circuits are protected by two 10 amp circuit breakers mounted in the
front panel. If these open, the contactor and wire feeder will not operate.
4. OVER TEMPERATURE PROTECTION
If the power source reaches an abnormally high internal temperature, the
thermal protection will deenergize the contactor circuit, shutting down the
power source but leaving the cooling fan on. After the power source has
cooled to a safe level, the thermal protection will automatically reset. While
de-energized, the contactor and wire feeder cannot be operated.
Page 27
DISCONNECT primary power at wall
switch, or circuit breaker, before attempting inspection or work inside
the power source.
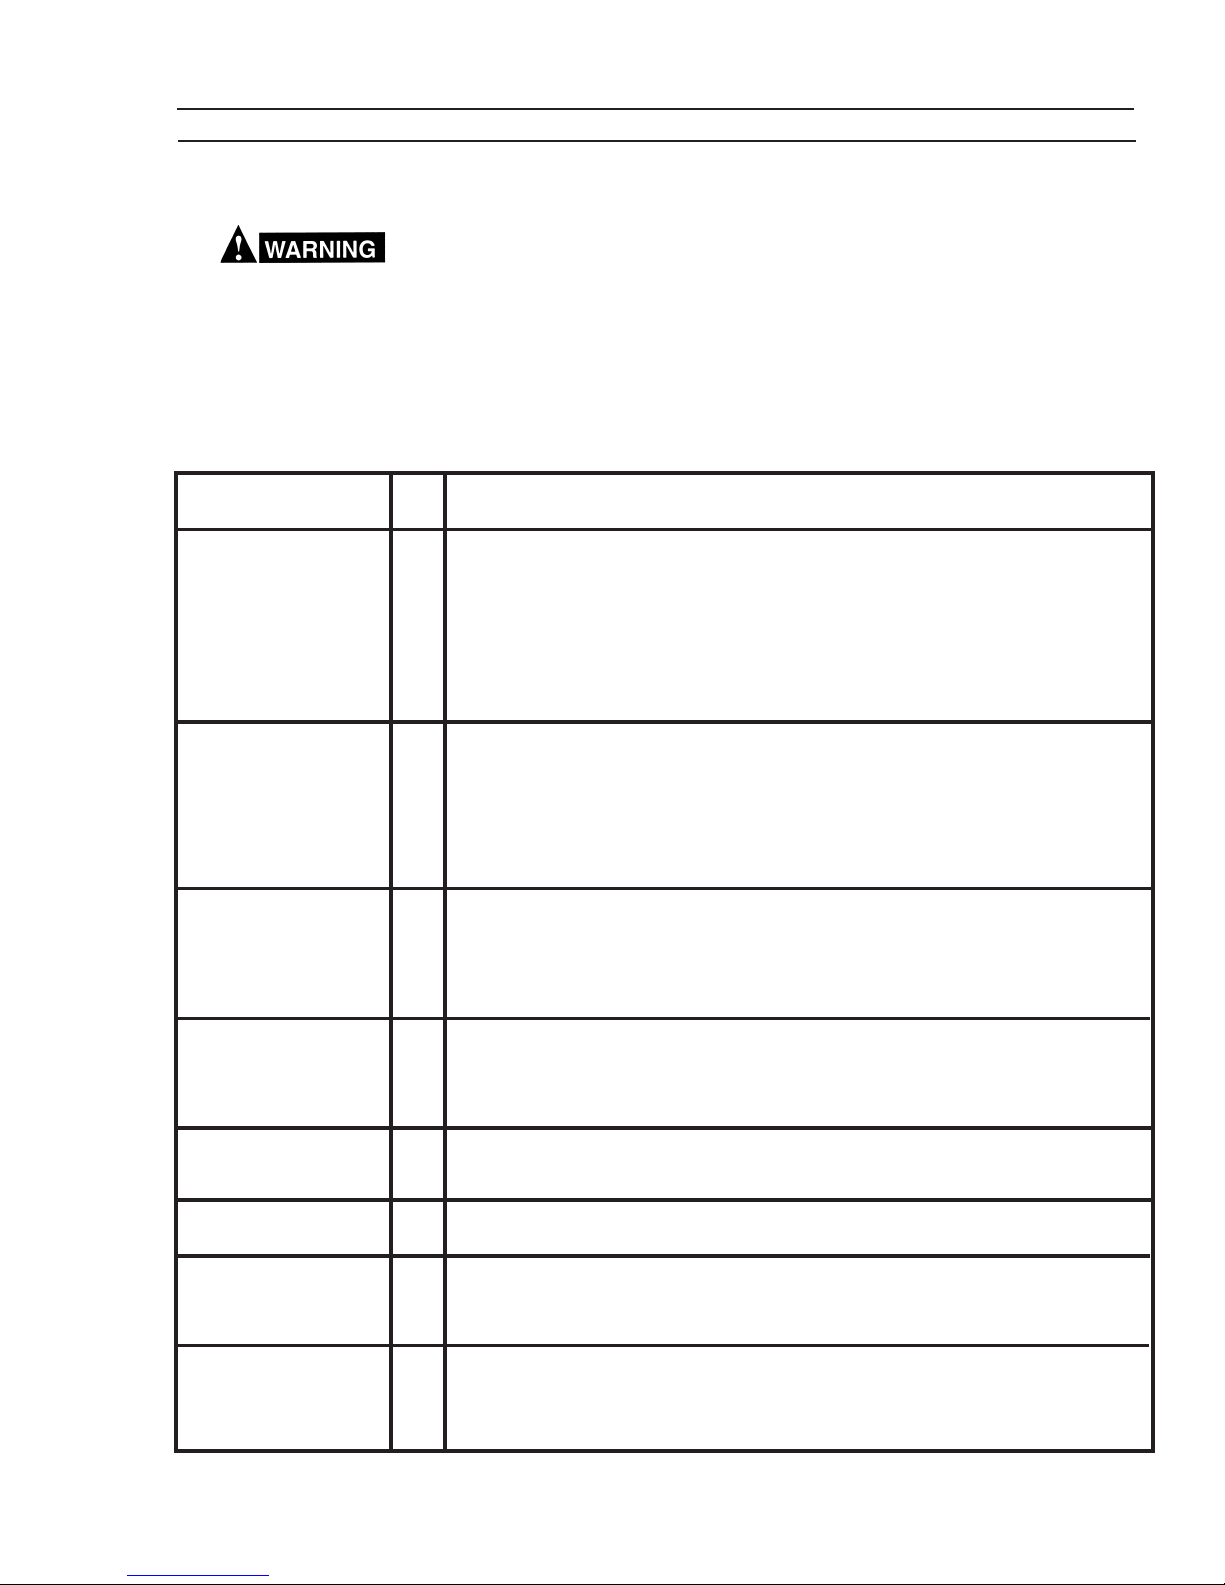
CONDITION ACTION
TROUBLESHOOTINGSECTION 7
VII. TROUBLESHOOTING
If the power source is operating improperly, the following troubleshooting
information may be used to locate the source of the trouble.
Check the problem against the symptoms in the following troubleshooting
guide (Table 7-1.) The remedy for the problem may be quite simple. If the cause
cannot be quickly located, open up the unit and perform a simple visual
inspection of all the components and wiring. Check for proper terminal
connections, loose or burned wiring or components, blown fuses, bulged or
leaking capacitors, or any other sign of damage or discoloration.
Table 7-1 Troubleshooting Table
Unit Inoperative A.
B.
C.
D.
E.
No Output -- Fan
Running
A.
B.
C.
D.
Limited Output or Low
A.
Open-Circuit Voltage
B.
C.
Erratic Weld Curre nt A.
B.
C.
D.
No input power. Check main line (user's) switch fuses -- replace if needed.
Poor or improper input (terminal board) connections.
Defective on/off switch on rear panel -- replace.
Thermal light on. Main transformer ove rheating. Also check for proper cooling,
proper primary hookup, or shorted turn on secondary.
Loss of primary phase. Find & replace defective fuse.
Poor or improper electrical input -- check input connections on TB.
Poor connections at output terminals/work station -- check, tighten or replace.
Main transformer overheating -- thermal switches tripped due to restricted cooling
air. Temperature light on front panel will be lit. Let unit cool down.
PC b oard de fective or loose PC board connector(s) -- if loose, reinsert; if
defective, replace.
Input voltage jumper links on terminal board improperly set -- check for proper
voltage.
Poor output connections. Take apart, clean, and reassemble.
Panel-Remote switch in Remote position and remote voltage pot disabled.
Welding cable size too small -- use correct cables.
Loose welding cable connec tion (will usually get hot) -- tighten all connections.
Improper wire feeder setup .
PC b oard de fective -- replace.
Hi gh Output, N o
A.B.PC b oard de fective or loose -- reset and/or replace board.
Voltage Control
No 115 Volt ac Output A. Circuit breaker tripped. Check 115V CB2 -- Reset.
Line Fuse Blows When
A.B.Shorted SCR in Main Bridge -- replace.
Power Source is First
Turned On
Wire Feeder is
A.B.Loose feeder control cable -- Check and tighten all connections.
Inoperative
Shorted I.G.B.T. - Replace I.G.B.T. and check driver PCB.
Shorted capacitor in Capacitor Bank.
A Circuit Breaker tripped -- Check 42V C B1 -- Reset.
Page 28
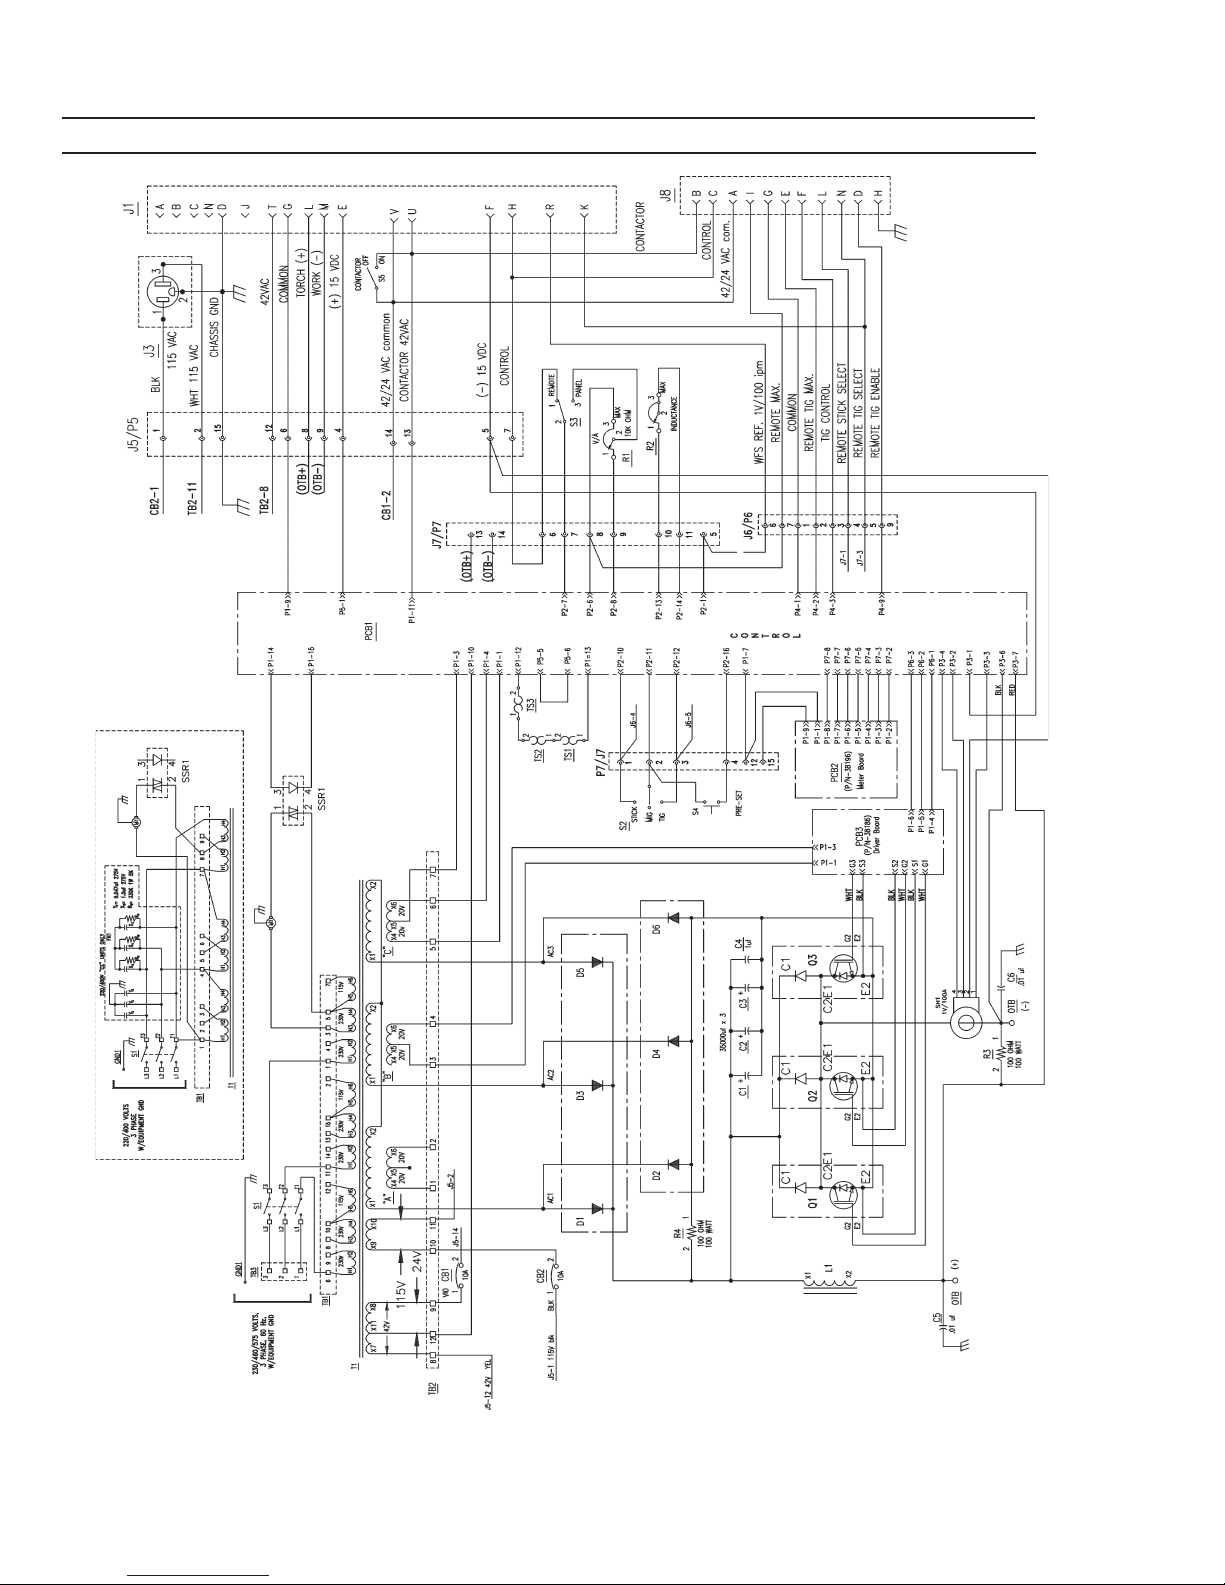
SECTION 8 REPLACEMENT PARTS
0558002702
28
Schematic Diagram - MultiPower 460 - 230/460/575V
28
Page 29
SECTION 8 REPLACEMENT PARTS
A. REPLACEMENT PARTS
Replacement Parts are illustrated on the following figures. When ordering replacement parts, order by part number and part name, as illustrated on the
figure. Always provide the series or serial number of the unit on which the parts
will be used. The serial number is stamped on the unit nameplate.
B. ORDERING
T o assure proper operation, it is recommended that only genuine ESAB parts
and products be used with this equipment. The use of non-ESAB parts may
void your warranty.
Replacement parts may be ordered from your ESAB distributor or from:
ESAB Welding & Cutting Products
Attn: Customer Service Dept.
P.O. Box 100545, 411 S. Ebenezer Road
Florence, SC 29501-0545
Be sure to indicate any special shipping instructions when ordering replacement parts.
T o order p arts by phone, contact ESAB at 1-843-664-5540. Orders may also
be faxed to 1-800-634-7548. Be sure to indicate any special shipping instructions when ordering replacement parts.
Refer to the Communication Guide located on the last page of this manual for
a list of customer service phone numbers.
29
Page 30
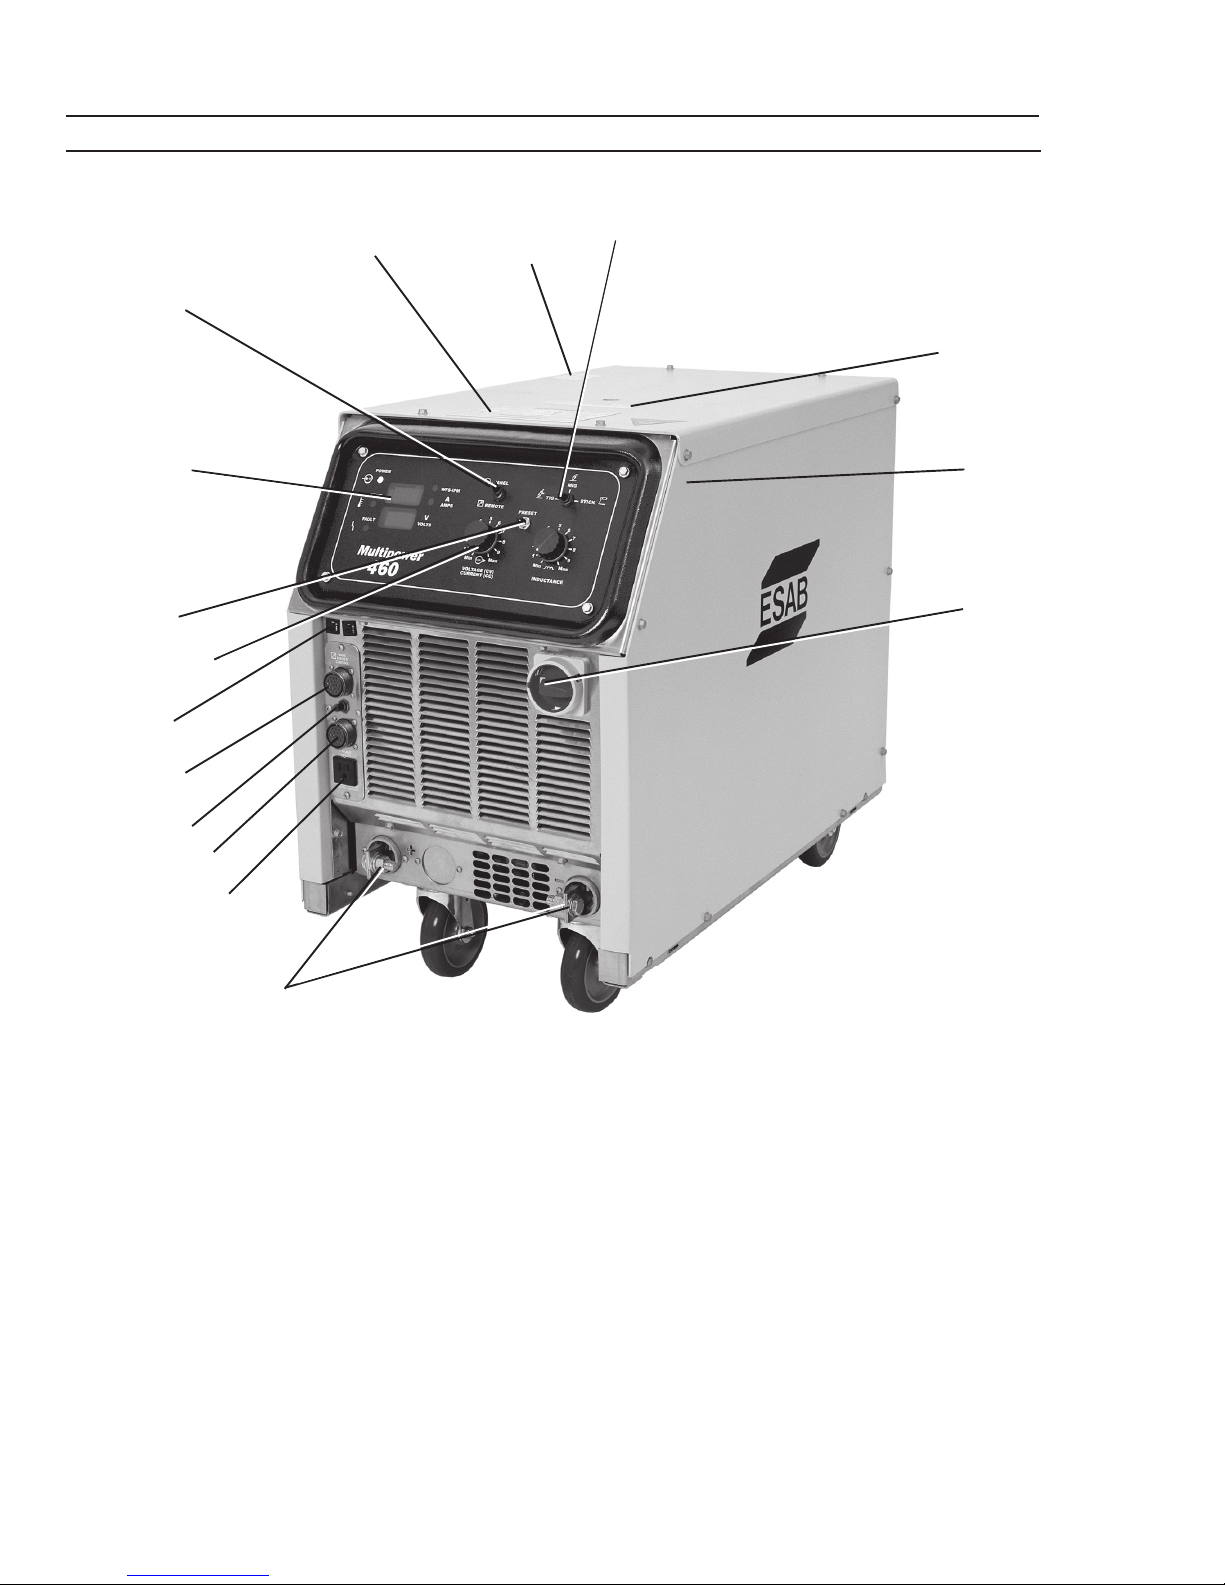
SECTION 8 REPLACEMENT PARTS
16
14
12, 13
15
17
9, 10
7
4, 5
11
18
19
8
6
3
2
1
Figure 8-1 - Front View, MultliPower 460
30
Page 31
SECTION 8 REPLACEMENT PARTS
Figure 8-1 - Front View, MultliPower 460
QTY . ITEM CIRCUIT
NO. REQ. NO. DESCRIPTION SYMBOL
1 2 678025 Terminal Assembly
2 1 952219 Outlet 110V (Square)
3 1 952937 Connection Box Rcpt. 14FS X-ROT
4 2 634515 SW TGGL SPDT 2 Pos 14A 125V Q/D S3, 5
5 3 951474 Switch Seal Black
6 1 952209 Recpt Panel 19 PIN F (Shell)
7 2 950122 Ckt Breaker 10A 32VDC/250VAC CB1, 2
8 2 0558001818 Knob 1.31 Dia.
9 2 13730632 Pot Lin *10.0K 2.00W 0.88L (A & B) R1, R2
10 1 952895 Switch PB Normally Open S4
11 1 38196 PCB Display Assembly PCB2
12 2 634515 SW TGGL SPDT 2 POS 14A 125V Q/D S3, 5
13 3 951474 Switch Seal Black
14 1 91514 Label Warning Arc Welding & Cutting
15 1 954008 Danger High Voltage
16 1 636702 SW TGGL SPDT 3 POS 10A 250V SCR S2
3 951474 Switch Seal Black
17 1 9512240 Label Caution Lifting Eye
18 1 0558002969 Panel Right Side
19 1 950945 SW Pwr Disc 100A 600V S1
31
Page 32
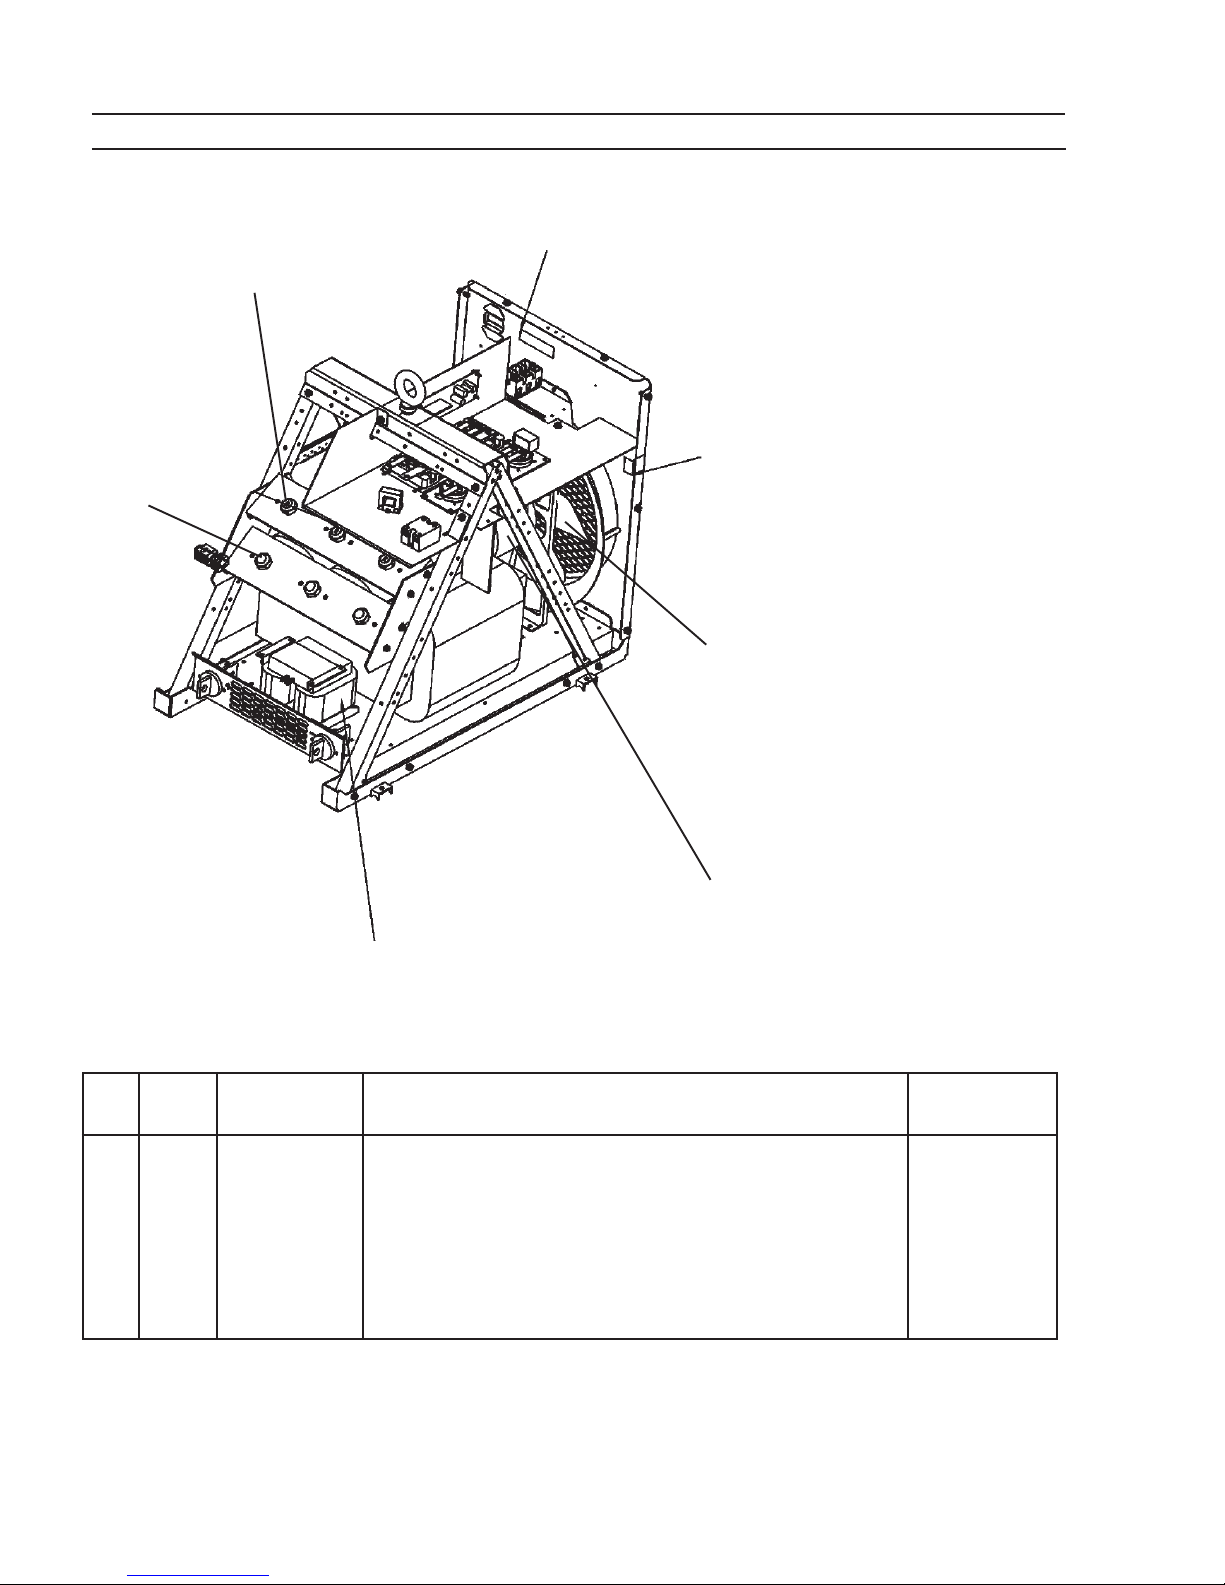
SECTION 8 REPLACEMENT PARTS
3
2
5
1
6
4
7
Figure 8-2 - Inside Front View, MultliPower 460
QTY. ITEM
NO. REQ. NO. DESCRIPTION SYMBOL
1 3 9951191 Diode Fwd 200V 250A
2 3 9951191 Diode Rev 200V 250A
3 1 954864 Label 3 Phase
4 1 2062334 Fan Motor 1/3 HP 1625 RPM
5 1 954699 Label Warning Fan Hazard
6 1 36173 Blade Fan 14" 5(or)6 Fin
7 1 33939 Inductor 7 Turn L2
32
Page 33
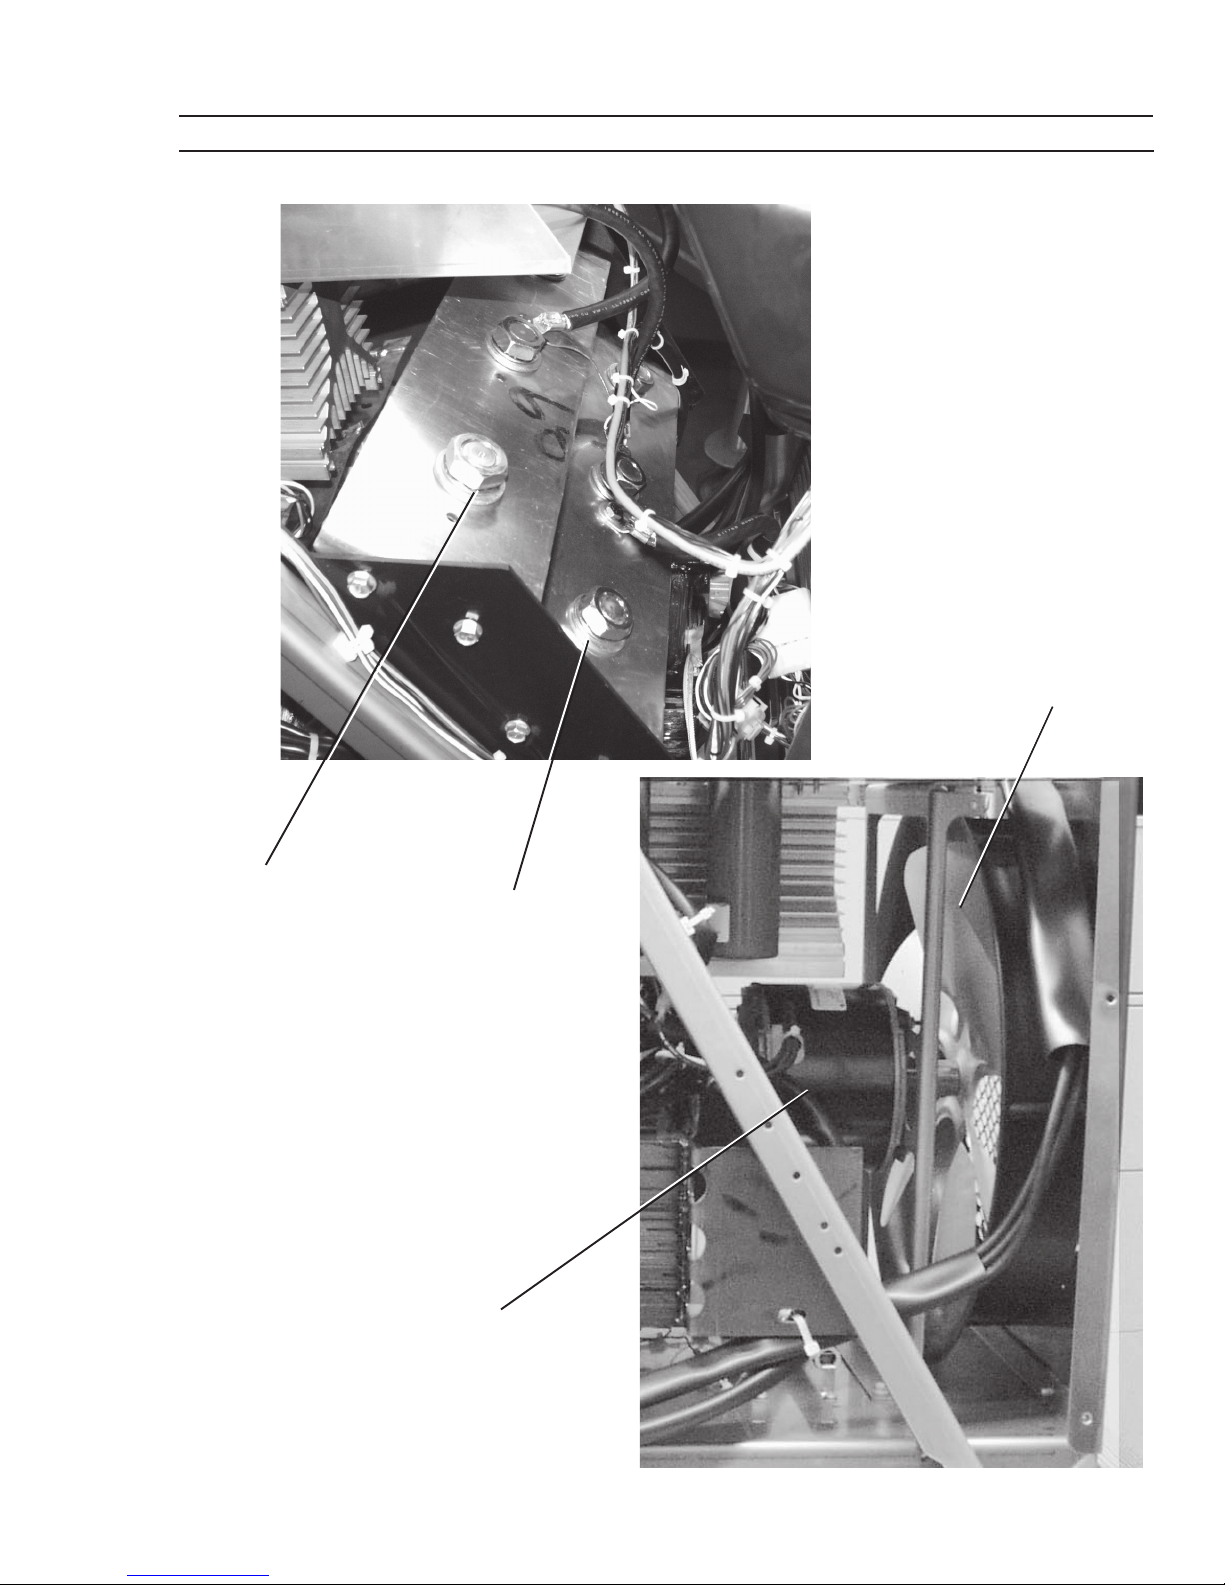
SECTION 8 REPLACEMENT PARTS
6
2
1
4
33
Page 34
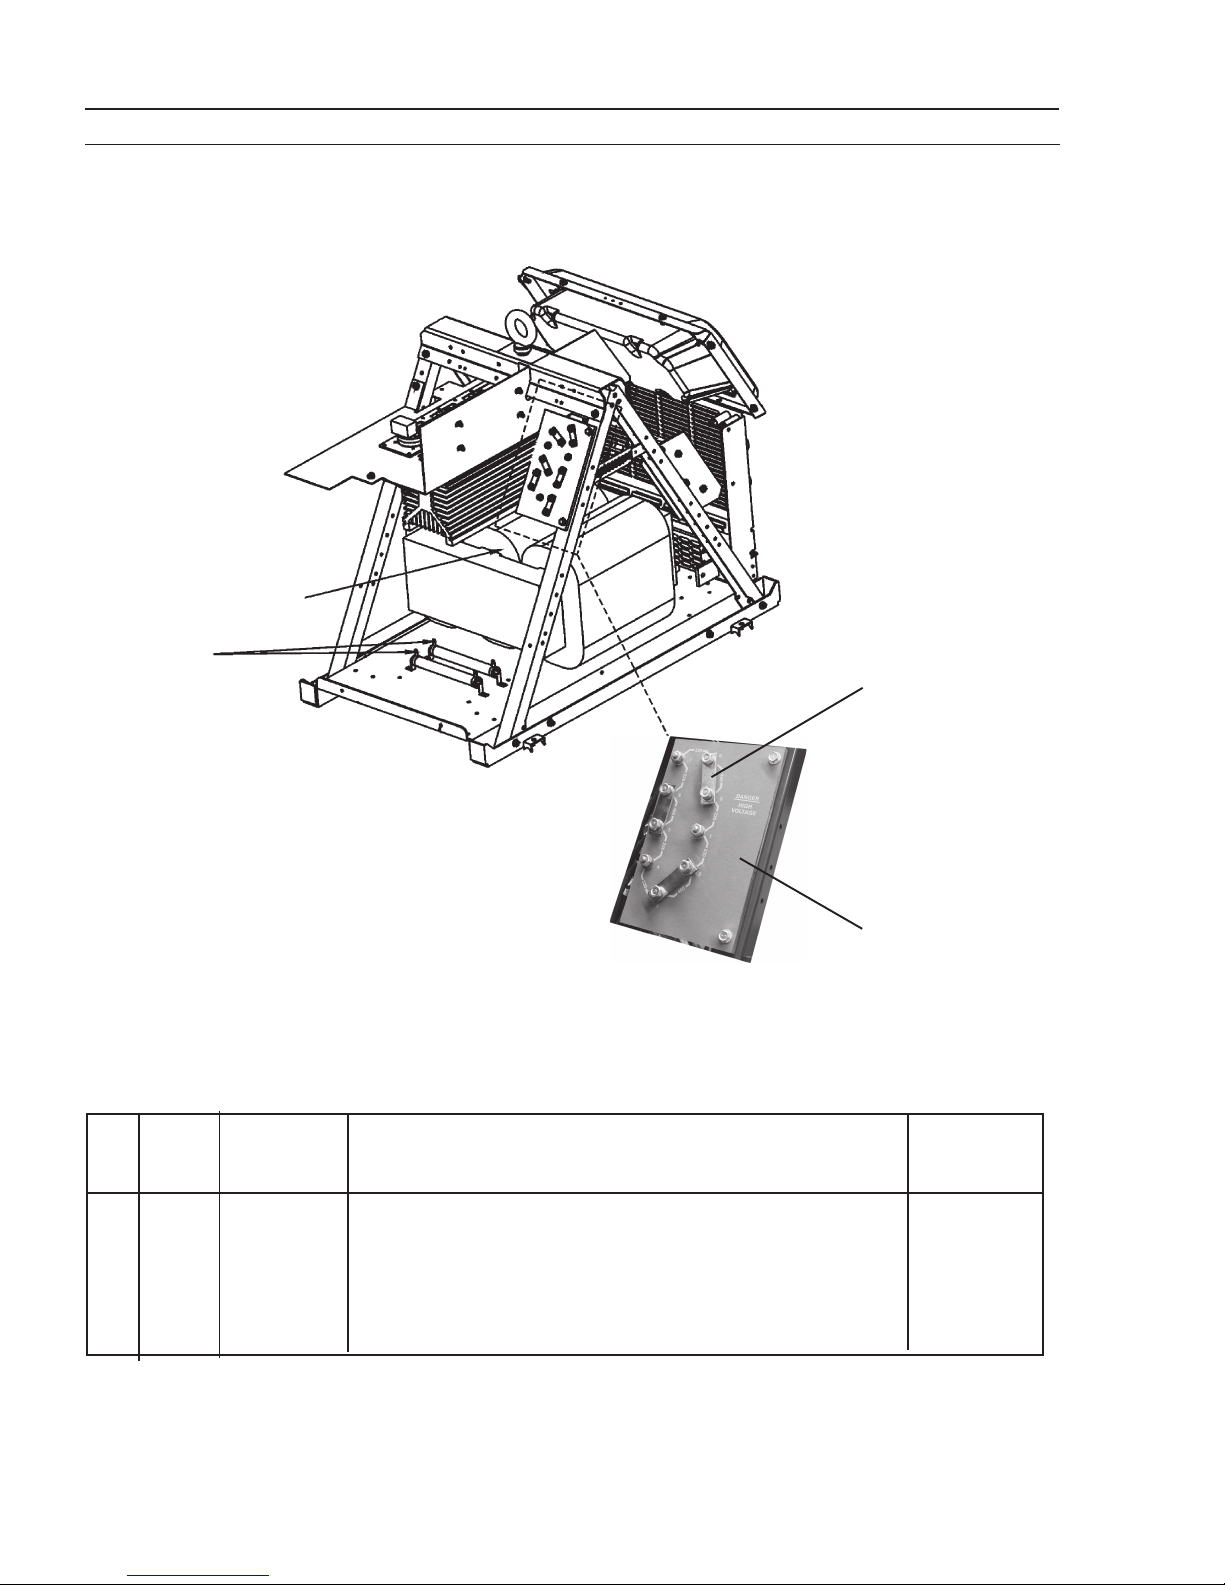
SECTION 8 REPLACEMENT PARTS
2
1
3
4
Figure 8-3 - Inside Rear View, MultliPower 460
QTY. ITEM
NO. REQ. NO. DESCRIPTION SYMBOL
1 2 17280110 Res WW Fix'd ST 100W 5% 100.00 R3, R4
2 1 0558002712 Transformer 230/460/575V T1
3 12 672065 Strap Terminal
4 20 3 6110 Board Input Terminal 230/460/575V
34
Page 35
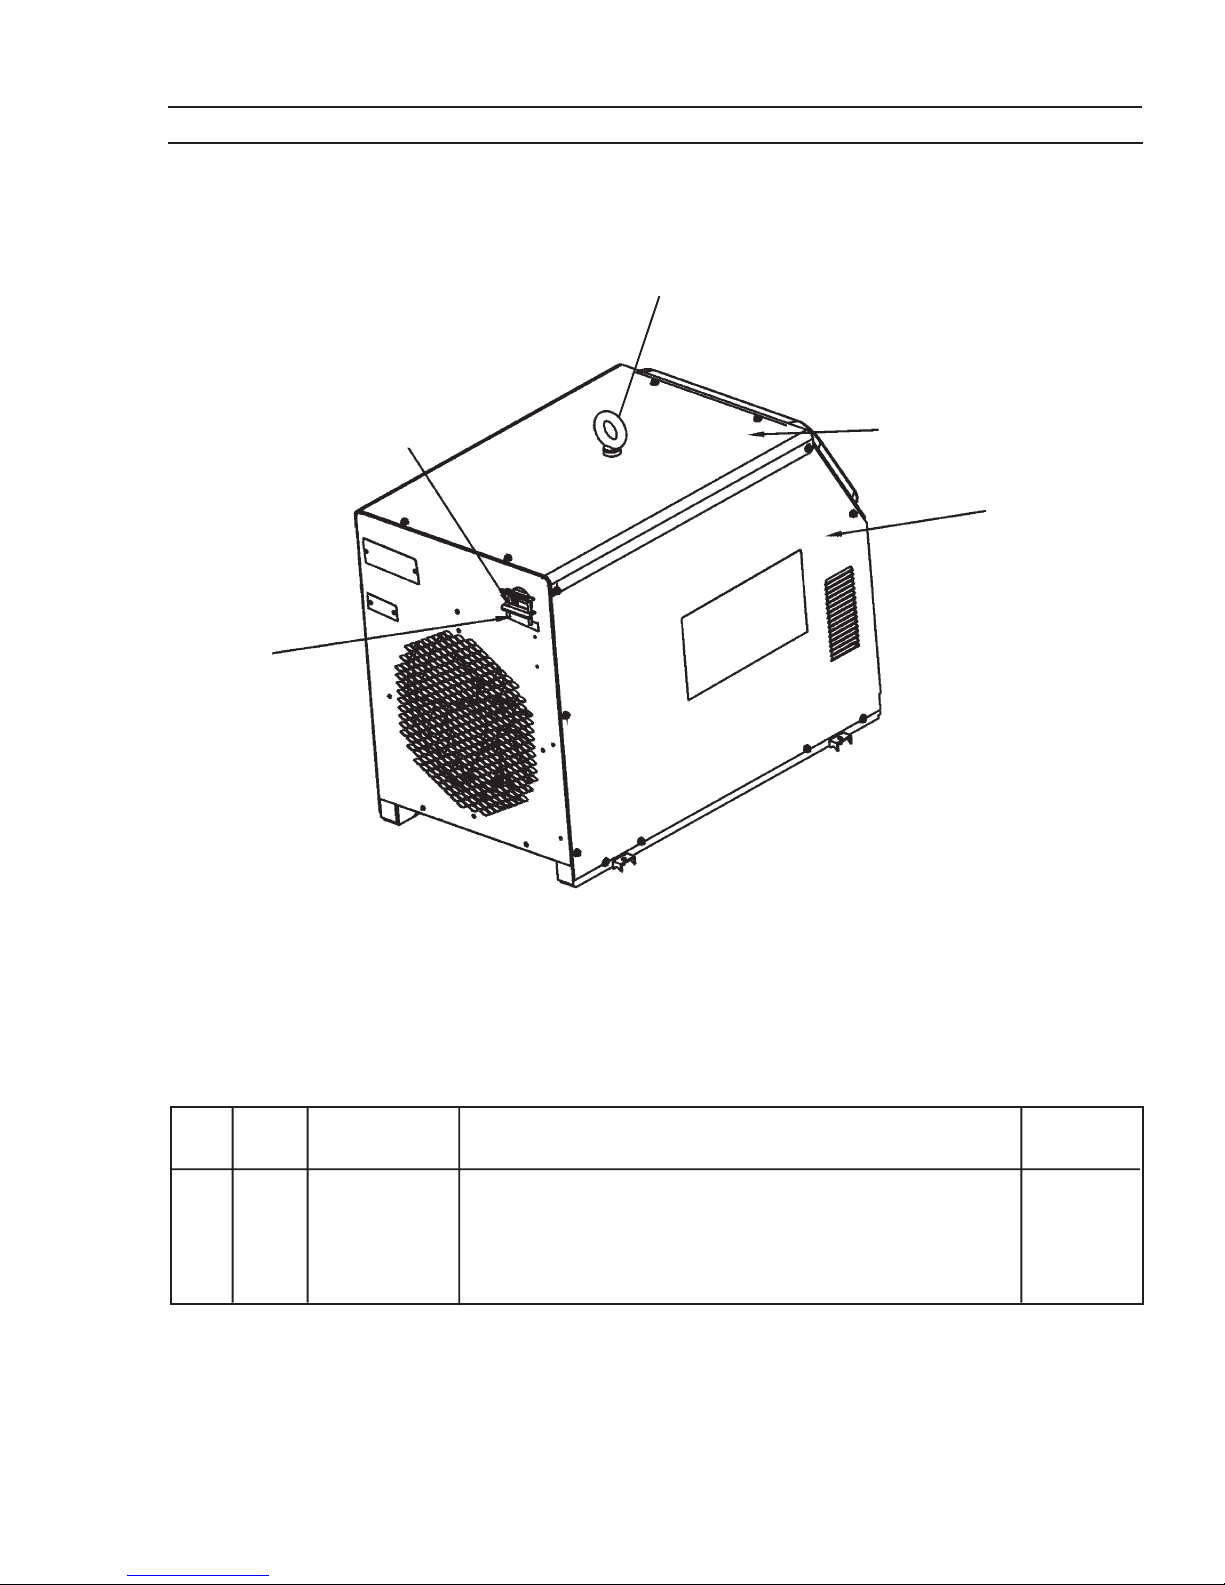
SECTION 8 REPLACEMENT PARTS
3
2
4
5
1
QTY . ITEM CIRCUIT
NO. REQ. NO. DESCRIPTION SYMBOL
1 1 1312733 Label for Install Use COP Wire
2 1 950219 Relief Strain 2" (Non-enclosed)
3 1 672786 Bolt Eye
4 1 0558001371 Panel Top Kydex Env
5 1 0558001370 Panel Left Side Kydex
Figure 8-4 External Rear View, MultliPower 460
35
Page 36
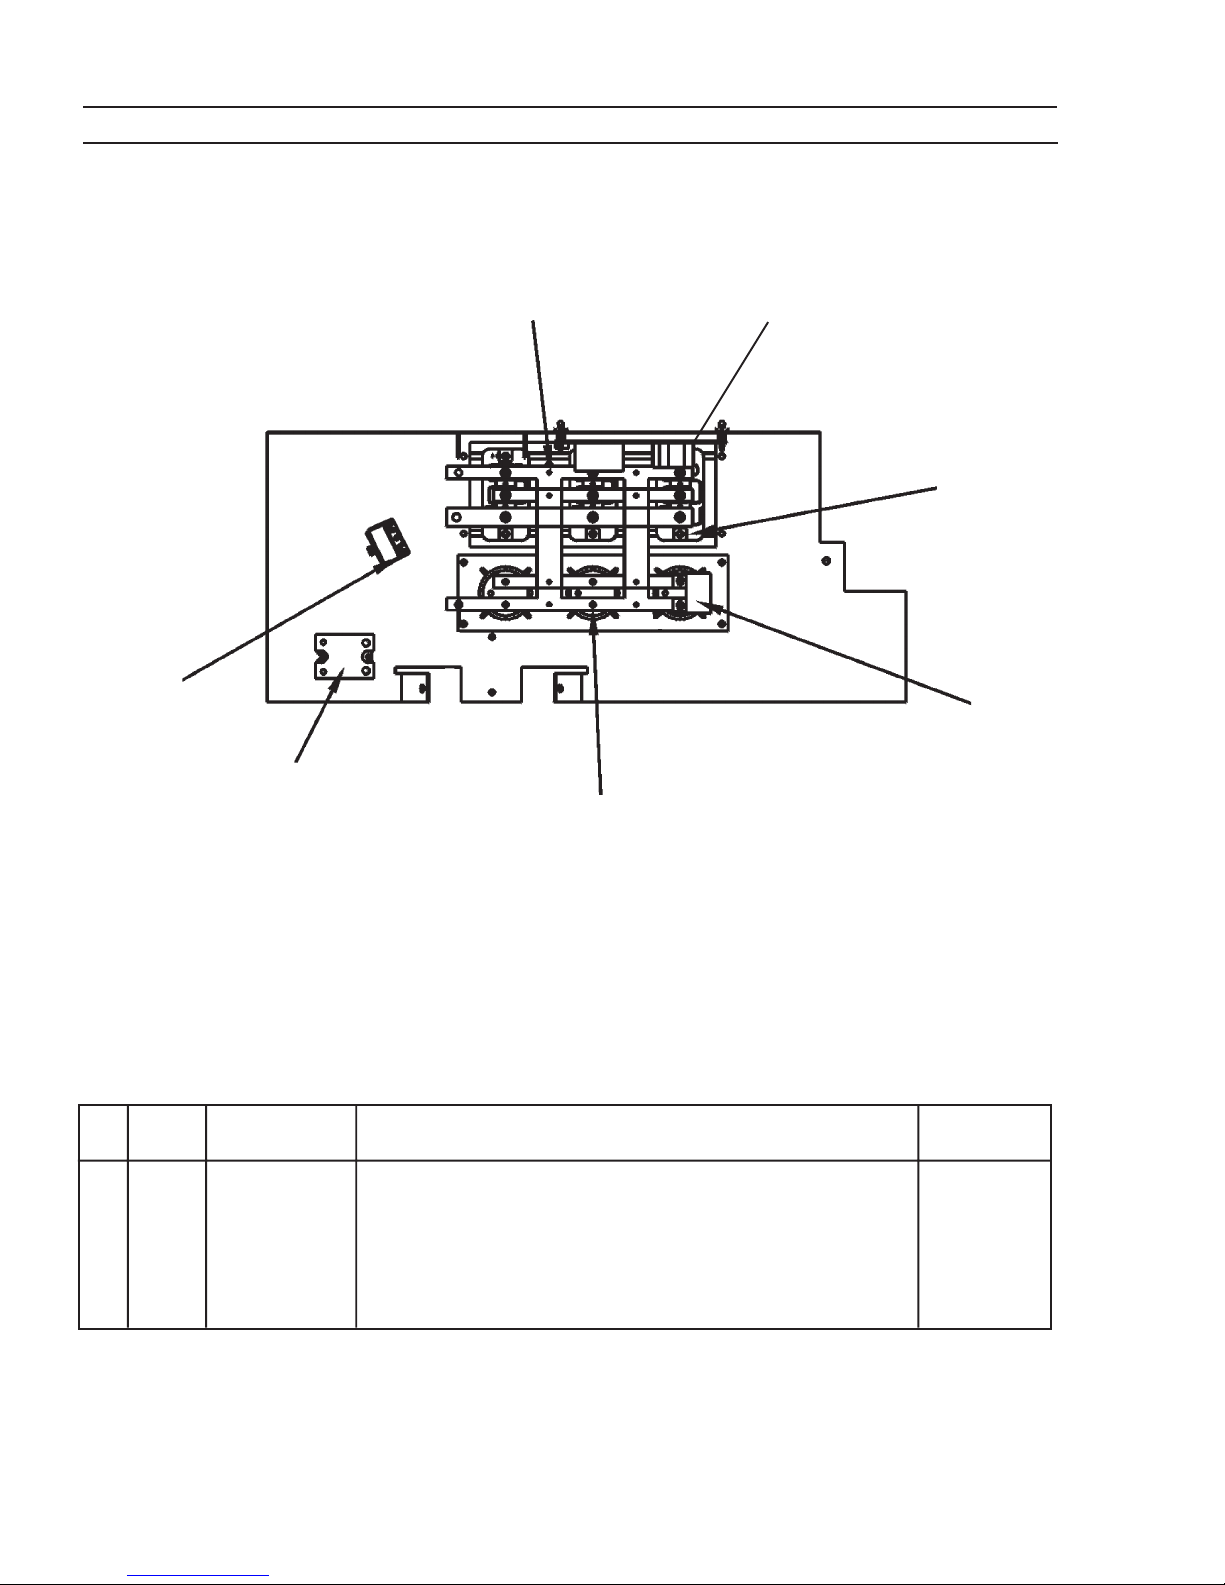
SECTION 8 REPLACEMENT
3
7
4
2
5
1
6
Figure 8-4 External Top View, MultliPower 460
QTY. ITEM
NO. REQ. NO. DESCRIPTION SYMBOL
1 1 952938 SCR 480V 18A Panel MNT
2 1 951997 Transducer Current SH1
3 1 951085 SW THML D/T 176 15A 120V Q/D TS6
4 3 0558003077 Matched Triple IGBT Kit - 600V/300A Q1, 2, 3
5 1 951940 Capacitor 1.0uf 600VDC 10% C4
6 3 0558002844 Capacitor, 35000UF 100VDC C1, 2, 3
7 1 38186 PCB Driver Assy . PCB3
Page 37
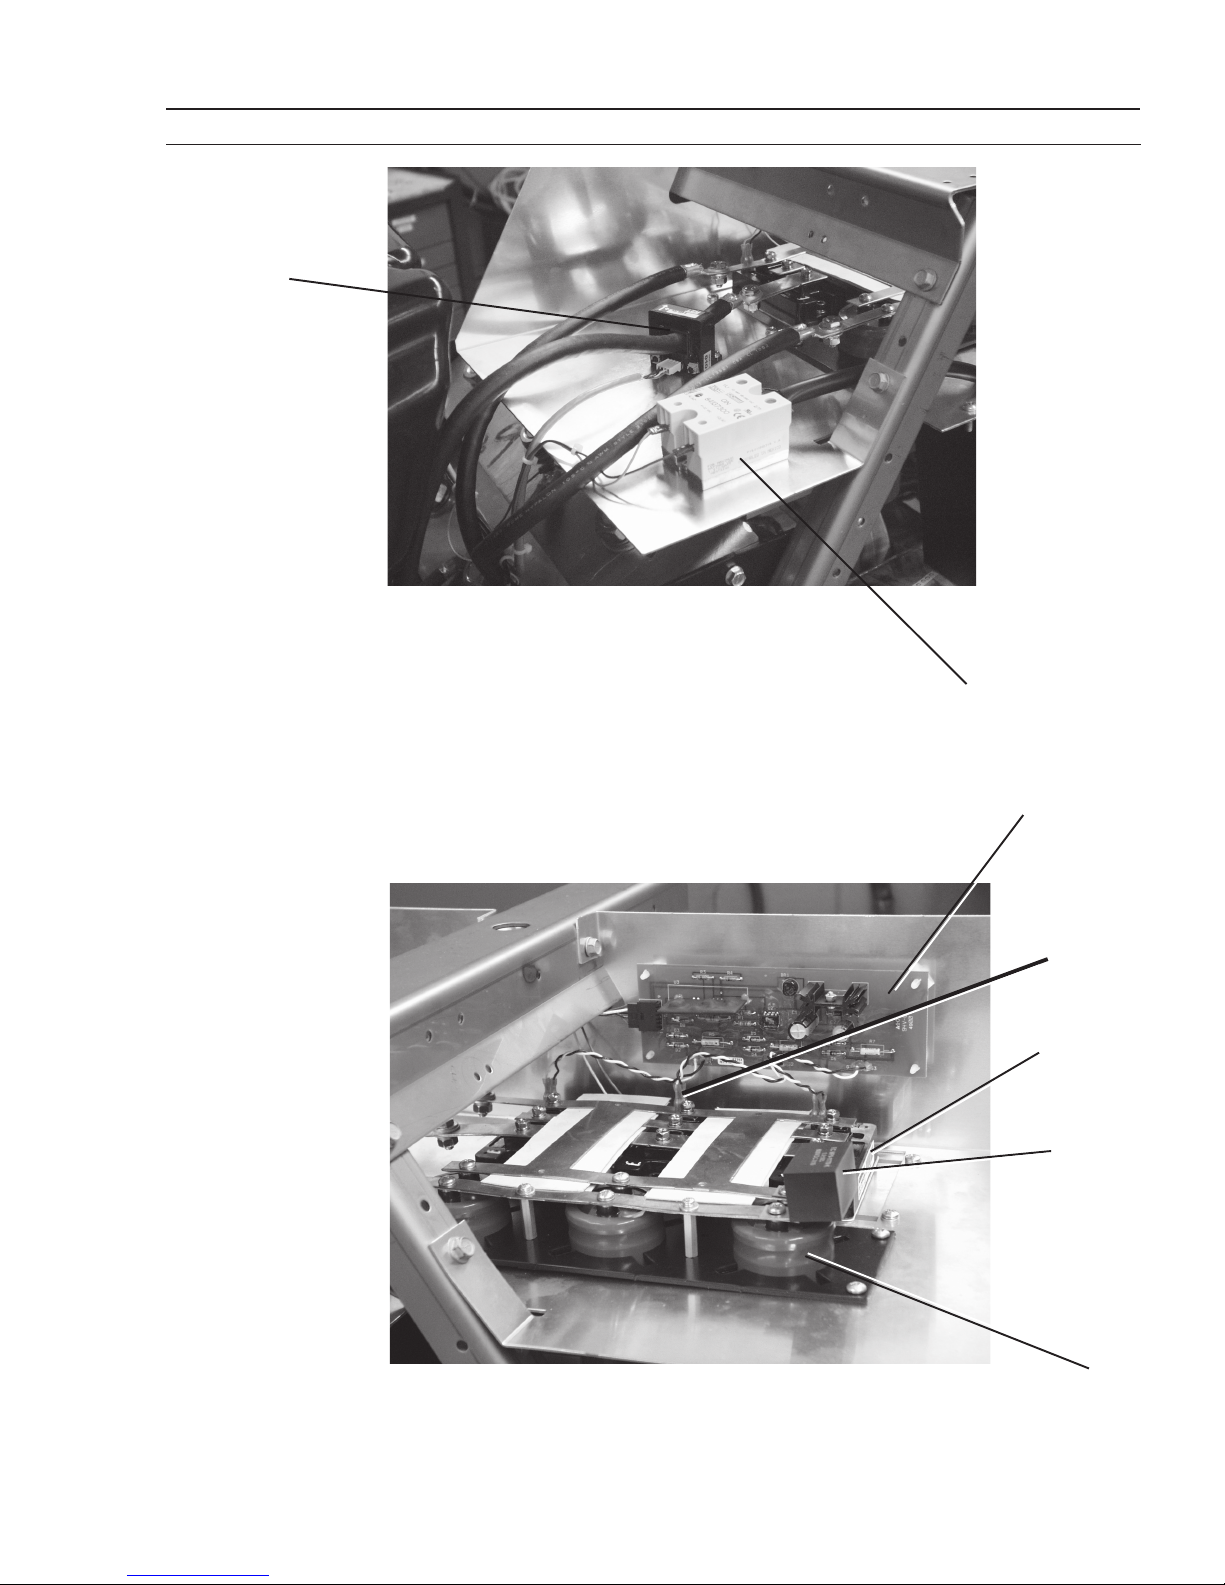
SECTION 8 REPLACEMENT PARTS
2
1
7
3
4
5
6
Page 38
SECTION 8 REPLACEMENT PARTS
38
Page 39
Revision History
Revision A: Updated primary power leads illustration and added input terminal board configurations. Changed IGBT item
number from 0558002557 to 0558003077 which is the matched triple IGBT kit.
Revision dated 07 / 2003: Five notes were added to Page 15 that provide information on the foot and / or the hand control
pendants. These were missing from earlier revisions of the manual.
39
Page 40
ESAB Welding & Cutting Products, Florence, SC Welding Equipment
COMMUNICATION GUIDE - CUSTOMER SERVICES
A. CUSTOMER SERVICE QUESTIONS:
Telephone: (800)362-7080 / Fax: (800) 634-7548 Hours: 8:00 AM to 7:00 PM EST
Order Entry Product Availability Pricing Order Information Returns
B. ENGINEERING SERVICE:
Telephone: (843) 664-4416 / Fax : (800) 446-5693 Hours: 7:30 AM to 5:00 PM EST
Warranty Returns Authorized Repair Stations Welding Equipment Troubleshooting
C. TECHNICAL SERVICE:
Telephone: (800) ESAB-123/ Fax: (843) 664-4452 Hours: 8:00 AM to 5:00 PM EST
Part Numbers Technical Applications Specifications Equipment Recommendations
D. LITERATURE REQUESTS:
Telephone: (843) 664-5562 / Fax: (843) 664-5548 Hours: 7:30 AM to 4:00 PM EST
E. WELDING EQUIPMENT REPAIRS:
Telephone: (843) 664-4487 / Fax: (843) 664-5557 Hours: 7:30 AM to 3:30 PM EST
Repair Estimates Repair Status
F. WELDING EQUIPMENT TRAINING
Telephone: (843)664-4428 / Fax: (843) 679-5864 Hours: 7:30 AM to 4:00 PM EST
Training School Information and Registrations
G. WELDING PROCESS ASSISTANCE:
Telephone: (800) ESAB-123 Hours: 7:30 AM to 4:00 PM EST
H. TECHNICAL ASST. CONSUMABLES:
Telephone : (800) 933-7070 Hours: 7:30 AM to 5:00 PM EST
IF YOU DO NOT KNOW WHOM TO CALL
Telephone: (800) ESAB-123
Fax: (843) 664-4452
Hours: 7:30 AM to 5:00 PM EST
or
visit us on the web at http://www.esabna.com
The ESAB web site offers
Comprehensive Product Information
Material Safety Data Sheets
Warranty Registration
Instruction Literature Download Library
Distributor Locator
Global Company Information
Press Releases
Customer Feedback & Support
F15-666-A 07 / 2003
 Loading...