

Page 1

EPP-200
Precision Plasmarc Cutting Console
Instruction ManualInstruction Manual
Instruction Manual
Instruction ManualInstruction Manual
0558004676 10 / 2007
Page 2

BE SURE THIS INFORMATION REACHES THE OPERATOR.
YOU CAN GET EXTRA COPIES THROUGH YOUR SUPPLIER.
CAUTION
These INSTRUCTIONS are for experienced operators. If you are not fully familiar with the
principles of operation and safe practices for arc welding and cutting equipment, we urge
you to read our booklet, “Precautions and Safe Practices for Arc Welding, Cutting, and
Gouging,” Form 52-529. Do NOT permit untrained persons to install, operate, or maintain
this equipment. Do NOT attempt to install or operate this equipment until you have read
and fully understand these instructions. If you do not fully understand these instructions,
contact your supplier for further information. Be sure to read the Safety Precautions before installing or operating this equipment.
USER RESPONSIBILITY
This equipment will perform in conformity with the description thereof contained in this manual and accompanying labels and/or inserts when installed, operated, maintained and repaired in accordance with the instructions provided. This equipment must be checked periodically. Malfunctioning or poorly maintained equipment
should not be used. Parts that are broken, missing, worn, distorted or contaminated should be replaced immediately. Should such repair or replacement become necessary, the manufacturer recommends that a telephone
or written request for service advice be made to the Authorized Distributor from whom it was purchased.
This equipment or any of its parts should not be altered without the prior written approval of the manufacturer.
The user of this equipment shall have the sole responsibility for any malfunction which results from improper
use, faulty maintenance, damage, improper repair or alteration by anyone other than the manufacturer or a service facility designated by the manufacturer.
READ AND UNDERSTAND THE INSTRUCTION MANUAL BEFORE INSTALLING OR OPERATING.
PROTECT YOURSELF AND OTHERS!
Page 3

TABLE OF CONTENTS
SECTIONSECTION
SECTION
SECTIONSECTION
PARAGRAPHPARAGRAPH
PARAGRAPH
PARAGRAPHPARAGRAPH
SECTION 1SECTION 1
SECTION 1
SECTION 1SECTION 1
SECTION 2SECTION 2
SECTION 2
SECTION 2SECTION 2
SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
SECTION 4SECTION 4
SECTION 4
SECTION 4SECTION 4
SECTION 5SECTION 5
SECTION 5
SECTION 5SECTION 5
SECTION 6SECTION 6
SECTION 6
SECTION 6SECTION 6
SECTION 7SECTION 7
SECTION 7
SECTION 7SECTION 7
TITLETITLE
TITLE
TITLETITLE
SAFETYSAFETY
SAFETY
SAFETYSAFETY
DESCRIPTIONDESCRIPTION
DESCRIPTION
DESCRIPTIONDESCRIPTION
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
OPERATIONOPERATION
OPERATION
OPERATIONOPERATION
MAINTENANCEMAINTENANCE
MAINTENANCE
MAINTENANCEMAINTENANCE
TROUBLESHOOTINGTROUBLESHOOTING
TROUBLESHOOTING
TROUBLESHOOTINGTROUBLESHOOTING
REPLACEMENT PARTSREPLACEMENT PARTS
REPLACEMENT PARTS
REPLACEMENT PARTSREPLACEMENT PARTS
....................................................................................................................................................................................
..........................................................................................
....................................................................................................................................................................................
..................................................................................................................................................................
.................................................................................
..................................................................................................................................................................
................................................................................................................................................................
................................................................................
................................................................................................................................................................
......................................................................................................................................................................
...................................................................................
......................................................................................................................................................................
..............................................................................................................................................................
...............................................................................
..............................................................................................................................................................
................................................................................................................................................
........................................................................
................................................................................................................................................
PAGEPAGE
PAGE
PAGEPAGE
..........................................................................................................................................
.....................................................................
..........................................................................................................................................
1111
11
1111
17
17
17
1717
2525
25
2525
2929
29
2929
3333
33
3333
3939
39
3939
55
5
55
3
Page 4

TABLE OF CONTENTSTABLE OF CONTENTS
TABLE OF CONTENTS
TABLE OF CONTENTSTABLE OF CONTENTS
4
Page 5

SECTION 1 SAFETY PRECAUTIONS
WARNING: These Safety Precautions are for
your protection. They summarize precautionary information from the references listed in
Additional Safety Information section. Before
performing any installation or operating procedures, be
sure to read and follow the safety precautions listed below
as well as all other manuals, material safety data sheets,
labels, etc. Failure to observe Safety Precautions can result
in injury or death.
PROTECT YOURSELF AND OTHERS
Some welding, cutting, and gouging processes are noisy and require ear protection. The arc, like the sun, emits ul-
traviolet (UV) and other radiation and
can injure skin and eyes. Hot metal can cause burns.
Training in the proper use of the processes and equipment is essential to prevent accidents. Therefore:
1. Always wear safety glasses with side shields in any work
area, even if welding helmets, face shields, and goggles
are also required.
2. Use a face shield fitted with the correct filter and cover
plates to protect your eyes, face, neck, and ears from
sparks and rays of the arc when operating or observing
operations. Warn bystanders not to watch the arc and not
to expose themselves to the rays of the electric-arc or hot
metal.
3. Wear flameproof gauntlet type gloves, heavy long-sleeve
shirt, cuffless trousers, high-topped shoes, and a welding helmet or cap for hair protection, to protect against
arc rays and hot sparks or hot metal. A flameproof apron
may also be desirable as protection against radiated
heat and sparks.
4. Hot sparks or metal can lodge in rolled up sleeves,
trouser cuffs, or pockets. Sleeves and collars should be
kept buttoned, and open pockets eliminated from the
front of clothing
5. Protect other personnel from arc rays and hot sparks with
a suitable non-flammable partition or curtains.
6. Use goggles over safety glasses when chipping slag or
grinding. Chipped slag may be hot and can fly far.
Bystanders should also wear goggles over safety glasses.
FIRES AND EXPLOSIONS -- Heat from
flames and arcs can start fires. Hot slag
or sparks can also cause fires and explosions. Therefore:
1. Remove all combustible materials well away from the
work area or cover the materials with a protective nonflammable covering. Combustible materials include
wood, cloth, sawdust, liquid and gas fuels, solvents,
paints and coatings, paper, etc.
2. Hot sparks or hot metal can fall through cracks or
crevices in floors or wall openings and cause a hidden
smoldering fire or fires on the floor below. Make certain
that such openings are protected from hot sparks and
metal.“
3. Do not weld, cut or perform other hot work until the
workpiece has been completely cleaned so that there
are no substances on the workpiece which might produce flammable or toxic vapors. Do not do hot work on
closed containers. They may explode.
4. Have fire extinguishing equipment handy for instant use,
such as a garden hose, water pail, sand bucket, or
portable fire extinguisher. Be sure you are trained in its
use.
5. Do not use equipment beyond its ratings. For example,
overloaded welding cable can overheat and create a fire
hazard.
6. After completing operations, inspect the work area to
make certain there are no hot sparks or hot metal which
could cause a later fire. Use fire watchers when necessary.
7. For additional information, refer to NFPA Standard 51B,
"Fire Prevention in Use of Cutting and Welding Pro-
--
cesses", available from the National Fire Protection Association, Batterymarch Park, Quincy, MA 02269.
ELECTRICAL SHOCK -- Contact with live
electrical parts and ground can cause
severe injury or death. DO NOT use AC
welding current in damp areas, if movement is confined, or if there is danger of
falling.
1. Be sure the power source frame (chassis) is connected
to the ground system of the input power.
2. Connect the workpiece to a good electrical ground.
3. Connect the work cable to the workpiece. A poor or
missing connection can expose you or others to a fatal
shock.
4. Use well-maintained equipment. Replace worn or damaged cables.
5. Keep everything dry, including clothing, work area,
cables, torch/electrode holder, and power source.
6. Make sure that all parts of your body are insulated from
work
and from ground.
7. Do not stand directly on metal or the earth while working
in tight quarters or a damp area; stand on dry boards or
an insulating platform and wear rubber-soled shoes.
8. Put on dry, hole-free gloves before turning on the power.
9. Turn off the power before removing your gloves.
10. Refer to ANSI/ASC Standard Z49.1 (listed on next page)
for specific grounding recommendations. Do not mistake the work lead for a ground cable.
ELECTRIC AND MAGNETIC FIELDS — May
be dangerous. Electric current flowing
through any conductor causes localized Electric and Magnetic Fields (EMF).
Welding and cutting current creates EMF
around welding cables and welding machines. Therefore:
1. Welders having pacemakers should consult their physician before welding. EMF may interfere with some pacemakers.
2. Exposure to EMF may have other health effects which are
unknown.
3. Welders should use the following procedures to minimize
exposure to EMF:
A. Route the electrode and work cables together. Secure
them with tape when possible.
B. Never coil the torch or work cable around your body.
C. Do not place your body between the torch and work
cables. Route cables on the same side of your body.
D. Connect the work cable to the workpiece as close as
possible to the area being welded.
E. Keep welding power source and cables as far away
from your body as possible.
5
Page 6

SECTION 1 SAFETY PRECAUTIONS
FUMES AND GASES -- Fumes and
gases, can cause discomfort or harm,
particularly in confined spaces. Do
not breathe fumes and gases. Shielding gases can cause asphyxiation.
Therefore:
1. Always provide adequate ventilation in the work area by
natural or mechanical means. Do not weld, cut, or gouge
on materials such as galvanized steel, stainless steel,
copper, zinc, lead, beryllium, or cadmium unless positive mechanical ventilation is provided. Do not breathe
fumes from these materials.
2. Do not operate near degreasing and spraying operations. The heat or arc rays can react with chlorinated
hydrocarbon vapors to form phosgene, a highly toxic
gas, and other irritant gases.
3. If you develop momentary eye, nose, or throat irritation
while operating, this is an indication that ventilation is not
adequate. Stop work and take necessary steps to improve ventilation in the work area. Do not continue to
operate if physical discomfort persists.
4. Refer to ANSI/ASC Standard Z49.1 (see listing below)
for specific ventilation recommendations.
5. WARNING: This product, when used for welding or
cutting, produces fumes or gases which
contain chemicals known to the State of
California to cause birth defects and, in
some cases, cancer. (California Health &
Safety Code
CYLINDER HANDLING -- Cylinders, if mishandled, can rupture and violently release gas. Sudden rupture of cylinder,
valve, or relief device can injure or kill.
Therefore:
1. Use the proper gas for the process and use the proper
pressure reducing regulator designed to operate from
the compressed gas cylinder. Do not use adaptors.
Maintain hoses and fittings in good condition. Follow
manufacturer's operating instructions for mounting regulator to a compressed gas cylinder.
2. Always secure cylinders in an upright position by chain
or strap to suitable hand trucks, undercarriages, benches,
walls, post, or racks. Never secure cylinders to work
tables or fixtures where they may become part of an
electrical circuit.
3. When not in use, keep cylinder valves closed. Have
valve protection cap in place if regulator is not connected. Secure and move cylinders by using suitable
hand trucks. Avoid rough handling of cylinders.
4. Locate cylinders away from heat, sparks, and flames.
Never strike an arc on a cylinder.
5. For additional information, refer to CGA Standard P-1,
"Precautions for Safe Handling of Compressed Gases in
Cylinders", which is available from Compressed Gas
Association, 1235 Jefferson Davis Highway, Arlington,
VA 22202.
§25249.5 et seq.)
EQUIPMENT MAINTENANCE -- Faulty or improperly maintained equipment can cause
injury or death. Therefore:
1. Always have qualified personnel perform the installation, troubleshooting, and maintenance work. Do not
perform any electrical work unless you are qualified to
perform such work.
2. Before performing any maintenance work inside a power
source, disconnect the power source from the incoming
electrical power.
3. Maintain cables, grounding wire, connections, power
cord, and power supply in safe working order. Do not
operate any equipment in faulty condition.
4. Do not abuse any equipment or accessories. Keep
equipment away from heat sources such as furnaces,
wet conditions such as water puddles, oil or grease,
corrosive atmospheres and inclement weather.
5. Keep all safety devices and cabinet covers in position
and in good repair.
6. Use equipment only for its intended purpose. Do not
modify it in any manner.
ADDITIONAL SAFETY INFORMATION -- For more
information on safe practices for electric arc
welding and cutting equipment, ask your supplier for a copy of "Precautions and Safe Practices for Arc Welding, Cutting and Gouging",
Form 52-529.
The following publications, which are available from the
American Welding Society, 550 N.W. LeJuene Road, Miami, FL 33126, are recommended to you:
1. ANSI/ASC Z49.1 - "Safety in Welding and Cutting"
2. AWS C5.1 - "Recommended Practices for Plasma Arc
Welding"
3. AWS C5.2 - "Recommended Practices for Plasma Arc
Cutting"
4. AWS C5.3 - "Recommended Practices for Air Carbon Arc
Gouging and Cutting"
5. AWS C5.5 - "Recommended Practices for Gas Tungsten
Arc Welding“
6. AWS C5.6 - "Recommended Practices for Gas Metal Arc
Welding"“
7. AWS SP - "Safe Practices" - Reprint, Welding Handbook.
8. ANSI/AWS F4.1, "Recommended Safe Practices for
Welding and Cutting of Containers That Have Held
Hazardous Substances."
MEANING OF SYMBOLS - As used throughout
this manual: Means Attention! Be Alert! Your
safety is involved.
Means immediate hazards which, if not
avoided, will result in immediate, serious personal injury or loss of life.
Means potential hazards which could
result in personal injury or loss of life.
Means hazards which could result in
minor personal injury.
6
Page 7

SECTION 1 PRECAUCION DE SEGURIDAD
ADVERTENCIA: Estas Precauciones de Seguridad
son para su protección. Ellas hacen resumen de
en la sección "Información Adicional Sobre La Seguridad". Antes
de hacer cualquier instalación o procedimiento de operación ,
asegúrese de leer y seguir las precauciones de seguridad listadas
a continuación así como también todo manual, hoja de datos de
seguridad del material, calcomanias, etc. El no observar las
Precauciones de Seguridad puede resultar en daño a la persona
ultravioleta (UV) y otras radiaciones que pueden dañar la
piel y los ojos. El metal caliente causa quemaduras. EL
entrenamiento en el uso propio de los equipos y sus
procesos es esencial para prevenir accidentes. Por lo
tanto:
información proveniente de las referencias listadas
o muerte
PROTEJASE USTED Y A LOS DEMAS-- Algunos
procesos de soldadura, corte y ranurado
son ruidosos y requiren protección para
los oídos. El arco, como el sol , emite rayos
.
1. Utilice gafas de seguridad con protección a los lados siempre
que esté en el área de trabajo, aún cuando esté usando careta
de soldar, protector para su cara u otro tipo de protección.
2. Use una careta que tenga el filtro correcto y lente para proteger
sus ojos, cara, cuello, y oídos de las chispas y rayos del arco
cuando se esté operando y observando las operaciones. Alerte
a todas las personas cercanas de no mirar el arco y no
exponerse a los rayos del arco eléctrico o el metal fundido.
3. Use guantes de cuero a prueba de fuego, camisa pesada de
mangas largas, pantalón de ruedo liso, zapato alto al tobillo, y
careta de soldar con capucha para el pelo, para proteger el
cuerpo de los rayos y chispas calientes provenientes del metal
fundido. En ocaciones un delantal a prueba de fuego es
necesario para protegerse del calor radiado y las chispas.
4. Chispas y partículas de metal caliente puede alojarse en las
mangas enrolladas de la camisa , el ruedo del pantalón o los
bolsillos. Mangas y cuellos deberán mantenerse abotonados,
bolsillos al frente de la camisa deberán ser cerrados o eliminados.
5. Proteja a otras personas de los rayos del arco y chispas
calientes con una cortina adecuada no-flamable como división.
6. Use careta protectora además de sus gafas de seguridad
cuando esté removiendo escoria o puliendo. La escoria puede
estar caliente y desprenderse con velocidad. Personas
cercanas deberán usar gafas de seguridad y careta protectora.
usted esta entrenado para su uso.
5. No use el equipo fuera de su rango de operación. Por ejemplo,
el calor causado por cable sobrecarga en los cables de soldar
pueden ocasionar un fuego.
6. Después de termirar la operación del equipo, inspeccione el área
de trabajo para cerciorarse de que las chispas o metal caliente
ocasionen un fuego más tarde. Tenga personal asignado para
vigilar si es necesario.
7. Para información adicional , haga referencia a la publicación
NFPA Standard 51B, "Fire Prevention in Use of Cutting and
Welding Processes", disponible a través de la National Fire
Protection Association, Batterymarch Park, Quincy, MA 02269.
CHOQUE ELECTRICO -- El contacto con las
partes eléctricas energizadas y tierra puede
causar daño severo o muerte. NO use
soldadura de corriente alterna (AC) en áreas
húmedas, de movimiento confinado en
lugares estrechos o si hay posibilidad de
caer al suelo.
1.
Asegúrese de que el chasis de la fuente de poder esté
conectado a tierra através del sistema de electricidad primario.
2. Conecte la pieza de trabajo a un buen sistema de tierra física.
3. Conecte el cable de retorno a la pieza de trabajo. Cables y
conductores expuestos o con malas conexiones pueden
exponer al operador u otras personas a un choque eléctrico
fatal.
4. Use el equipo solamente si está en buenas condiciones.
Reemplaze cables rotos, dañados o con conductores
expuestos.
5. Mantenga todo seco, incluyendo su ropa, el área de trabajo, los
cables, antorchas, pinza del electrodo, y la fuente de poder.
6. Asegúrese que todas las partes de su cuerpo están insuladas
de ambos, la pieza de trabajo y tierra.
7. No se pare directamente sobre metal o tierra mientras trabaja
en lugares estrechos o áreas húmedas; trabaje sobre un
pedazo de madera seco o una plataforma insulada y use
zapatos con suela de goma.
8. Use guantes secos y sin agujeros antes de energizar el equipo.
9. Apage el equipo antes de quitarse sus guantes.
10. Use como referencia la publicación ANSI/ASC Standard Z49.1
(listado en la próxima página) para recomendaciones específicas
de como conectar el equipo a tierra. No confunda el cable de
soldar a la pieza de trabajo con el cable a tierra.
FUEGO Y EXPLOSIONES -- El calor de las
flamas y el arco pueden ocacionar fuegos.
Escoria caliente y las chispas pueden
causar fuegos y explosiones. Por lo tanto:
1.
Remueva todo material combustible lejos del área de trabajo o
cubra los materiales con una cobija a prueba de fuego.
Materiales combustibles incluyen madera, ropa, líquidos y
gases flamables, solventes, pinturas, papel, etc.
2. Chispas y partículas de metal pueden introducirse en las grietas
y agujeros de pisos y paredes causando fuegos escondidos en
otros niveles o espacios. Asegúrese de que toda grieta y
agujero esté cubierto para proteger lugares adyacentes contra
fuegos.
3. No corte, suelde o haga cualquier otro trabajo relacionado hasta
que la pieza de trabajo esté totalmente limpia y libre de
substancias que puedan producir gases inflamables o vapores
tóxicos. No trabaje dentro o fuera de contenedores o tanques
cerrados. Estos pueden explotar si contienen vapores
inflamables.
4. Tenga siempre a la mano equipo extintor de fuego para uso
instantáneo, como por ejemplo una manguera con agua, cubeta
con agua, cubeta con arena, o extintor portátil. Asegúrese que
CAMPOS ELECTRICOS Y MAGNETICOS - Son
peligrosos. La corriente eléctrica fluye através
de cualquier conductor causando a nivel local
Campos Eléctricos y Magnéticos (EMF). Las
corrientes en el área de corte y soldadura,
crean EMF alrrededor de los cables de soldar
y las maquinas. Por lo tanto:
1. S
oldadores u Operadores que use marca-pasos para el corazón
deberán consultar a su médico antes de soldar. El Campo
Electromagnético (EMF) puede interferir con algunos marcapasos.
2. Exponerse a campos electromagnéticos (EMF) puede causar
otros efectos de salud aún desconocidos.
3. Los soldadores deberán usar los siguientes procedimientos para
minimizar exponerse al EMF:
A. Mantenga el electrodo y el cable a la pieza de trabajo juntos,
hasta llegar a la pieza que usted quiere soldar. Asegúrelos uno
junto al otro con cinta adhesiva cuando sea posible.
B. Nunca envuelva los cables de soldar alrededor de su cuerpo.
C. Nunca ubique su cuerpo entre la antorcha y el cable, a la pieza
de trabajo. Mantega los cables a un sólo lado de su cuerpo.
D. Conecte el cable de trabajo a la pieza de trabajo lo más cercano
posible al área de la soldadura.
E . Mantenga la fuente de poder y los cables de soldar lo más lejos
7
posible de su cuerpo.
Page 8

SECTION 1 PRECAUCION DE SEGURIDAD
HUMO Y GASES -- El humo y los gases,
pueden causar malestar o daño,
particularmente en espacios sin
ventilación. No inhale el humo o gases. El
gas de protección puede causar falta de
oxígeno.
Por lo tanto:
1. Siempre provea ventilación adecuada en el área de
trabajo por medio natural o mecánico. No solde, corte, o
ranure materiales con hierro galvanizado, acero inoxidable,
cobre, zinc, plomo, berílio, o cadmio a menos que provea
ventilación mecánica positiva . No respire los gases
producidos por estos materiales.
2. No opere cerca de lugares donde se aplique substancias
químicas en aerosol. El calor de los rayos del arco pueden
reaccionar con los vapores de hidrocarburo clorinado
para formar un fosfógeno, o gas tóxico, y otros irritant es.
3. Si momentáneamente desarrolla inrritación de ojos, nariz
o garganta mientras est á operando, es indicación de que
la ventilación no es apropiada. Pare de trabajar y tome
las medidas necesarias para mejorar la ventilación en
el área de trabajo. No continúe operando si el malestar
físico persiste.
4. Haga referencia a la publicación ANSI/ASC Standard
Z49.1 (Vea la lista a continuación) para recomendaciones
específicas en la ventilación.
5. ADVERTENCIA-- Este producto cuando se utiliza para
soldaduras o cortes, produce humos
o gases, los cuales contienen
químicos conocidos por el Estado
de California de causar defectos en
el nacimiento, o en algunos casos,
Cancer. (California Health & Safety
Code
§25249.5 et seq.)
MANEJO DE CILINDROS-- Los
cilindros, si no son manejados
correctamente, pueden romperse y
liberar violentamente gases. Rotura
repentina del cilindro, válvula, o
válvula de escape puede causar daño
o muerte. Por lo tanto:
1. Utilize el gas apropiado para el proceso y utilize un
regulador diseñado para operar y reducir la presión del
cilindro de gas . No utilice adaptadores. Mantenga las
mangueras y las conexiones en buenas condiciones.
Observe las instrucciones de operación del manufacturero
para montar el regulador en el cilindro de gas comprimido.
2. Asegure siempre los cilindros en posición vertical y
amárrelos con una correa o cadena adecuada para
asegurar el cilindro al carro, transportes, tablilleros, paredes,
postes, o armazón. Nunca asegure los cilindros a la mesa
de trabajo o las piezas que son parte del circuito de
soldadura . Este puede ser parte del circuito elélectrico.
3. Cuando el cilindro no está en uso, mantenga la válvula del
cilindro cerrada. Ponga el capote de protección sobre la
válvula si el regulador no está conectado. Asegure y
mueva los cilindros utilizando un carro o transporte
adecuado. Evite el manejo brusco de los
MANTENIMIENTO DEL EQUIPO -- Equipo
defectuoso o mal mantenido puede causar
daño o muerte. Por lo tanto:
1. Siempre tenga personal cualificado para efectuar l
a instalación, diagnóstico, y mantenimiento del
equipo. No ejecute ningún trabajo eléctrico a menos
que usted esté cualificado para hacer el trabajo.
2. Antes de dar mantenimiento en el interior de la
fuente de poder, desconecte la fuente de poder del
suministro de electricidad primaria.
3. Mantenga los cables, cable a tierra, conexciones,
cable primario, y cualquier otra fuente de poder en
buen estado operacional. No opere ningún equipo
en malas condiciones.
4. No abuse del equipo y sus accesorios. Mantenga el
equipo lejos de cosas que generen calor como
hornos, también lugares húmedos como charcos de
agua , aceite o grasa, atmósferas corrosivas y las
inclemencias del tiempo.
5. Mantenga todos los artículos de seguridad y coverturas
del equipo en su posición y en buenas condiciones.
6. Use el equipo sólo para el propósito que fue diseñado.
No modifique el equipo en ninguna manera.
INFORMACION ADICIONAL DE SEGURIDAD -Para más información sobre las prácticas de
seguridad de los equipos de arco eléctrico para
soldar y cortar, pregunte a su suplidor por una
copia de "Precautions and Safe Practices for Arc
Welding, Cutting and Gouging-Form 52-529.
Las siguientes publicaciones, disponibles através de la
American Welding Society, 550 N.W. LeJuene Road, Miami,
FL 33126, son recomendadas para usted:
1. ANSI/ASC Z49.1 - "Safety in Welding and Cutting"
2. AWS C5.1 - "Recommended Practices for Plasma Arc
Welding"
3. AWS C5.2 - "Recommended Practices for Plasma Arc
Cutting"
4. AWS C5.3 - "Recommended Practices for Air Carbon Arc
Gouging and Cutting"
5. AWS C5.5 - "Recommended Practices for Gas Tungsten
Arc Welding“
6. AWS C5.6 - "Recommended Practices for Gas Metal Arc
Welding"“
7. AWS SP - "Safe Practices" - Reprint, Welding Handbook.
8. ANSI/AWS F4.1, "Recommended Safe Practices for Welding and Cutting of Containers That Have Held Hazardous
Substances."
SIGNIFICADO DE LOS SIMBOLOS -- Según
usted avanza en la lectura de este folleto:
Los Símbolos Significan ¡Atención! ¡Esté
Alerta! Se trata de su seguridad.
Significa riesgo inmediato que, de no ser
evadido, puede resultar inmediatamente
en serio daño personal o la muerte.
Significa el riesgo de un peligro potencial
que puede resultar en serio daño personal o la muerte.
Significa el posible riesgo que puede
resultar en menores daños a la persona.
8
Page 9

SECTION 1 PRÉCAUTIONS DE SÉCURITÉ
AVERTISSEMENT: Ces règles de sécurité ont pour objet
d’ assurer votre protection. Veillez à lire et à observer les
précautions énoncées ci-dessous avant de monter l’
équipement ou de commercer à l’utiliser. Tout défaut
d’observation de ces précautions risque d’entraîner des
blessures graves ou mortelles.
1. PROTECTION INDIVIDUELLE-- Les brûlures de la
peau et des yeux dues au rayonnement de l’arc
électrique ou du métal incandescent, lors du soudage
au plasma ou à l’électrode ou lors du gougeage à
l’arc, peuvent s’avérer plus graves que celles résultant
d’une exposition prolongée au soleil. Aussi convientil d’observer les précautions suivantes:
a. Portez un écran facial adéquat muni des plaques
protectrices et des verres filtrants appropriés afin de
vous protéger les yeux, le visage, le cou et les
oreilles des étincelles et du rayonnement de l’arc
électrique lorsque vous effectuez des soudures ou
des coupes ou lorsque vous en observez l’exécution.
AVERTISSEZ les personnes se trouvant à proximité
de façon à ce qu’elles ne regardent pas l’arc et à ce
qu’elles ne s’exposent pas à son rayonnement, ni à
celui du métal incandescent.
b. Portez des gants ignifugés à crispins, une tunique
épaisse à manches longues, des pantalons sans
rebord, des chaussures à embout d’acier et un
casque de soudage ou une calotte de protection, afin
d’éviter d’exposer la peau au rayonnement de l’arc
électrique ou du métal incandescent. ll est également
souhaitable d’utiliser un tablier ininflammable de
façon à se protéger des étincelles et du rayonnement
thermique.
c. Les étincelles ou les projections de métal incandes-
cent risquent de se loger dans des manches
retroussées, des bords relevés de pantalons ou dans
des poches. Aussi convient-il de garder boutonnés le
col et les manches et de porter des vêtements sans
poches à l’avant.
d. Protégez des étincelles et du rayonnement de l’arc
électrique les autres personnes travaillant à proximité
à l’aide d’un écran ininflammable adéquat.
e. Ne jamais omettre de porter des lunettes de sécurité
lorsque vous vous trouvez dans un secteur où l’on
effectue des opérations de soudage ou de coupage à
l’arc. Utilisez des lunettes de sécurité à écrans ou
verres latéraux pour piquer ou meûler le laitier. Les
piquetures incandescentes de laitier peuvent être
projetées à des distances considérables. Les
personnes se trouvant à proximité doivent également
porter des lunettes de protection.
f. Le gougeage à l’arc et le soudage à l’arc au plasma
produisent un niveau de bruit extrêmement élevé (de
100 à 114 dB) et exigent par conséquent l’emploi de
dispositifs appropriés de protection auditive.
2 PRÉVENTION DES INCENDES-- Les projections de
laitier incandescent ou d’étincelles peuvent provoquer
de graves incendies au contact de matériaux combustibles solides, liquides ou gazeux. Aussi faut-il
observer les précautions suivantes:
a. Éloigner suffisamment tous les matériaux combustibles
du secteur où l’on exécute des soudures ou des coupes
à l’arc, à moins de les recouvrir complètement d’une
bâche non-inflammable. Ce type de matériaux comprend
notamment le bois, les vêtements, la sciure, l’essence,
le kérosène, les peintures, les solvants, le gaz naturel,
l’acétylène, le propane et autres substances combustibles semblables.
b. Les étincelles ou les projections de métal incandescent
peuvent tomber dans des fissures du plancher ou dans
des ouvertures des murs et y déclencher une ignition
lente cachée. Veiller à protéger ces ouvertures des
étincelles et des projections de métal.
c. N’exécutez pas de soudures, de coupes, d’opérations
de gougeage ou autres travaux à chaud à la surface de
barils, bidons, réservoirs ou autres contenants usagés,
avant de les avoir nettoyés de toute trace de substance
susceptible de produire des vapeurs inflammables ou
toxiques.
d. En vue d’assurer la prévention des incendies, il convient
de disposer d’un matériel d’extinction prêt à servir
immédiatement, tel qu’un tuyau d’arrosage, un seau à
eau, un seau de sable ou un extincteur portatif.
e. Une fois le travail à l’arc terminé, inspectez le secteur de
façon à vous assurer qu’aucune étincelle ou projection
de métal incandescent ne risque de provoquer
ultérieurement un feu.
3. CHOC ÉLECTRIQUE-- Le gougeage à l’arc et à l’arc au
plasma exige l’emploi de tensions à vide relativement
importantes; or, celles-ci risquent de causer des
dommages corporels graves et même mortels en cas
d’utilisation inadéquate. La gravité du choc électrique
reçu dépend du chemin suivi par le courant à travers le
corps humain et de son intensité.
a. Ne laissez jamais de surfaces métalliques sous tension
venir au contact direct de la peau ou de vêtements
humides. Veillez à porter des gants bien secs.
b. Si vous devez effectuer un travail sur une surface
métallique ou dans un secteur humide, veillez à assu-rer
votre isolation corporelle en portant des gants secs et
des chaussures à semelles de caoutchouc et en vous
tenant sur une planche ou une plate-forme sèche.
c. Mettez toujours à la terre le poste de soudage/coupage
en le reliant par un câble à une bonne prise de terre.
d. N’utilisez jamais de câbles usés ou endommagés. Ne
surchargez jamais le câble. Utilisez toujours un
équipement correctement entretenu.
e. Mettez l’équipement hors tension lorsqu’il n’est pas en
service. une mise à la masse accidentelle peut en effet
provoquer une surchauffe de l’équipement et un danger
d’incendie. Ne pas enrouler ou passer le câble autour
d’une partie quelconque du corps.
f. Vérifiez si le câble de masse est bien relié à la pièce en
un point aussi proche que possible de la zone de travail.
Le branchement des câbles de masse à l’ossature du
bâtiment ou en un point éloigné de la zone de travail
augmente en effet le risque de passage d’un courant de
sortie par des chaînes de
9
Page 10

SECTION 1 PRÉCAUTIONS DE SÉCURITÉ
levage, des câbles de grue ou divers chemins
électriques.
g. Empêchez l’apparition de toute humidité, notamment
sur vos vêtements, à la surface de l’emplacement de
travail, des câbles, du porte-électrode et du poste de
soudage/coupage. Réparez immédiatement toute
fuite d’eau.
4. VENTILATION-- La respiration prolongée des fumées
résultant des opérations de soudage/coupage, à
l’intérieur, d’un local clos, peut provoquer des malaises et des dommages corporels. Aussi convient-il
d’observer les précautions suivantes:
a. Assurez en permanence une aération adéquate de
l’emplacement de travail en maintenant une ventilation naturelle ou à l’aide de moyens mécaniques.
N’effectuez jamais de travaux de soudage ou de
coupage sur des matériaux de zinc, de plomb, de
beryllium ou de cadmium en l’absence de moyens
mécaniques de ventilation capables d’empêcher
l’inhalation des fumées dégagées par ces matériaux.
b. N’effectuez jamais de travaux de soudage ou de
coupage à proximité de vapeurs d’hydrocarbure
chloré résultant d’opérations voisines de dégraissage
ou de pulvérisation. La chaleur dégagée ou le
rayonnement de l’arc peut déclencher la formation de
phosgène -- gaz particulièrement toxique -- et d’autres
gaz irritants, à partir des vapeurs de solvant.
c. Une irritation momentanée des yeux, du nez ou de la
gorge constatée au cours de l’utilisation de
l’équipement dénote un défaut de ventilation. Arrêtezvous de travailler afin de prendre les mesures nécessaires à l’amélioration de la ventilation. Ne poursuivez
pas l’opération entreprise si le malaise persiste.
d. Certaines commandes comportent des canalisations
où circule de l’hydrogène. L’armoire de commande
est munie d’un ventilateur destiné à empêcher la
formation de poches d’hydrogène, lesquelles
présentent un danger d’explosion; ce ventilateur ne
fonctionne que si l’interrupteur correspondant du
panneau avant se trouve placé en position ON
(Marche). Veillez à manœuvrer cette commande en
vérifiant si le couvercle est bien en place, de façon à
assurer l’efficacité de la ventilation ainsi réalisée. Ne
jamais débrancher le ventilateur.
e. Les fumées produites par l’opération de soudage ou
de coupage peuvent s’avérer toxiques. Aussi est-il
nécessaire de disposer en permanence d’un dispositif
adéquat de ventilation de type aspirant, afin d’éliminer du voisinage de l’opérateur tout dégagement de
fumée visible.
f. Consultez les recommandations particulières en
matière de ventilation indiquées à l’alinéa 6 de la
norme Z49.1 de l’AWS.
5. ENTRETIEN DE L’ÉQUIPEMENT-- Un équipement
entretenu de façon défectueuse ou inadéquate risque
non seulement de réaliser un travail de mauvaise
qualité mais, chose plus grave encore, d’entraîner des
dommages corporels graves, voire mortels en
déclenchant des incendies ou des chocs électriques.
Observez par conséquent les précautions suivantes:
a. Efforcez-vous de toujours confier à un personnel qua-
lifié l’installation, le dépannage et l’entretien du poste
de soudage et de coupage. N’effectuez aucune
réparation électrique sur l’équipement à moins d’être
qua-lifié à cet effet.
b. Ne procédez jamais à une tâche d’entretien quelconque
à l’intérieur du poste de soudage/coupage, avant
d’avoir débranché l’alimentation électrique.
c . Maintenez en bon état de fonctionnement les câbles,
le câble de masse, les branchements, le cordon
d’alimentation et le poste de soudage/coupage.
N’utilisez jamais le poste ou l’équipement s’il présente
une défectuosité quelconque.
d. Prenez soin du poste de soudage et de coupage et
des équipements accessoires. Gardez-les à l’écart
des sources de charleur, notamment des fours, de
l’humidité, des flaques d’eau maintenez-les à l’abri
des traces d’huile ou de graisse, des atmosphères
corrosives et des intempéries.
e. Laissez en place tous les dispositifs de sécurité et
tous les panneaux de l’armoire de commande en
veillant à les garder en bon état.
f. Utilisez le poste de soudage/coupage conformément
à son usage prévu et n’effectuez aucune modification.
6. INFORMATIONS COMPLÉMENTAIRES RELATIVES
À LA SÉCURITÉ--
Pour obtenir des informations complémentaires sur
les règles de sécurité à observer pour le montage et
l’utilisation d’équipements de soudage et de coupage
électriques et sur les méthodes de travail
recommandées, demandez un exemplaire du livret N°
52529 “Precautions and Safe Practices for Arc Welding, Cutting and Gouging” publié par ESAB. Nous
conseillons également de consulter les publications
sui-vantes, tenues à votre disposition par l’American
Welding Society, 550 N.W. LeJuene Road, Miami, FL
32126:
a. “Safety in Welding and Cutting” AWS Z49.1
b. “Recommended Safe Practices for Gas-Shielded Arc
Welding “AWS A6. 1.
c. “Safe Practices for Welding and Cutting Containers
That Have Held Combustibles” AWS-A6.0.
d. “Recommended Safe Practices for Plasma Arc
Cutting” AWS-A6. 3.
e. “Recommended Safe Practices for Plasma Arc
Welding” AWS-C5. 1.
f. “Recommended Safe Practices for Air Carbon Arc
Gouging and Cutting” AWS-C5. 3.
g. “Code For Safety in Welding and Cutting” CSA-St andard
W117. 2.
10
Page 11

SECTION 2SECTION 2
SECTION 2
SECTION 2SECTION 2
2.1 Introduction
DESCRIPTIONDESCRIPTION
DESCRIPTION
DESCRIPTIONDESCRIPTION
The EPP 200 Power Console is designed for mechanized plasma
applications. It can be used with other ESAB products such as the
PT-24 and PT-600 torches, an optional plumbing box and a remote
set-up pendant.
• 50 to 200 Amperes cutting current range
• Forced air cooled
• Solid state DC power
• Integral water cooler
• Input voltage protection
• Local or remote front panel control
• Thermal switch protection for main transformer and
power semiconductor components
• LED status troubleshooting
2.2 General Specifications
EPP 200 Power Console (0558004315):
OUTPUT (100% duty cycle)
Voltage ............................................................................160VDC
Current range DC.........................................................50A to 200A
Power .....................................................................8000 W to 32000 W
Open Circuit Voltage (OCV).............................................325VDC
INPUT
Voltage (3-phase) .......................................... 200/230/380/415/460/575 Volts
Current (3-phase) ............................................ 115/100/60/55/50/40 Amperes
Frequency........................................................................ 50/60Hz
KVA................................................................................. 39.8 kW
Power .............................................................................. 37.8 kW
Power Factor ...................................................................... 95%
Input Fuse ...........................................................See Section 3, Installation
11
Page 12

SECTION 2 DESCRIPTION
Electric Shock Can Kill!
WARNINGWARNING
WARNING
WARNINGWARNING
2.3 Dimensions and Weight
Use of torches not designed for this console could result in
a hazardous electric shock.
Use only torches designed for the EPP-200 Console.
22in. (550mm)
42in. (1050mm)
44 in. (1100mm)
Weight = 725 lbs. (330 kg)
12
Page 13

SECTION 2 DESCRIPTION
2.4 EPP-200 Options and Accessories
Options
5 ft. (1.5m)
10 ft. (3.0m)
20 ft. (6.1m)
25 ft. (7.6m)
30 ft. (9.1m)
40 ft. (12.2m)
50 ft. (15.2m)
75 ft. (22.9m)
100 ft. (30.5m)
125 ft. (38.1m)
150 ft. (45.7m)
* Cooling Water Hoses (2)
Console to Plumbing Box
0558003979
0558003980
0558003981
33132
0558003982
0558003983
33133
33134
33135
33136
0558003984
Control Cable
Plumbing Box to Console
N / A
N / A
N / A
0558004651
N / A
N / A
0558004652
0558004653
0558004654
0558003978
0558004655
* Use with one adaptor fitting (41V12) included with unit.
Pilot Arc Lead
Plumbing Box to Console
0558003985
0558003986
0558003987
33303
0558003988
0558003989
33304
33305
33306
33307
0558003990
Power Lead
Console to Plumbing Box
0558003991
0558003992
0558003993
22001
0558003994
0558003995
22002
22003
22004
22005
0558003996
Torch Coolant – 1gallon (3.8 L) - (4 required) = 156F05
13
Page 14
SECTION 2 DESCRIPTION
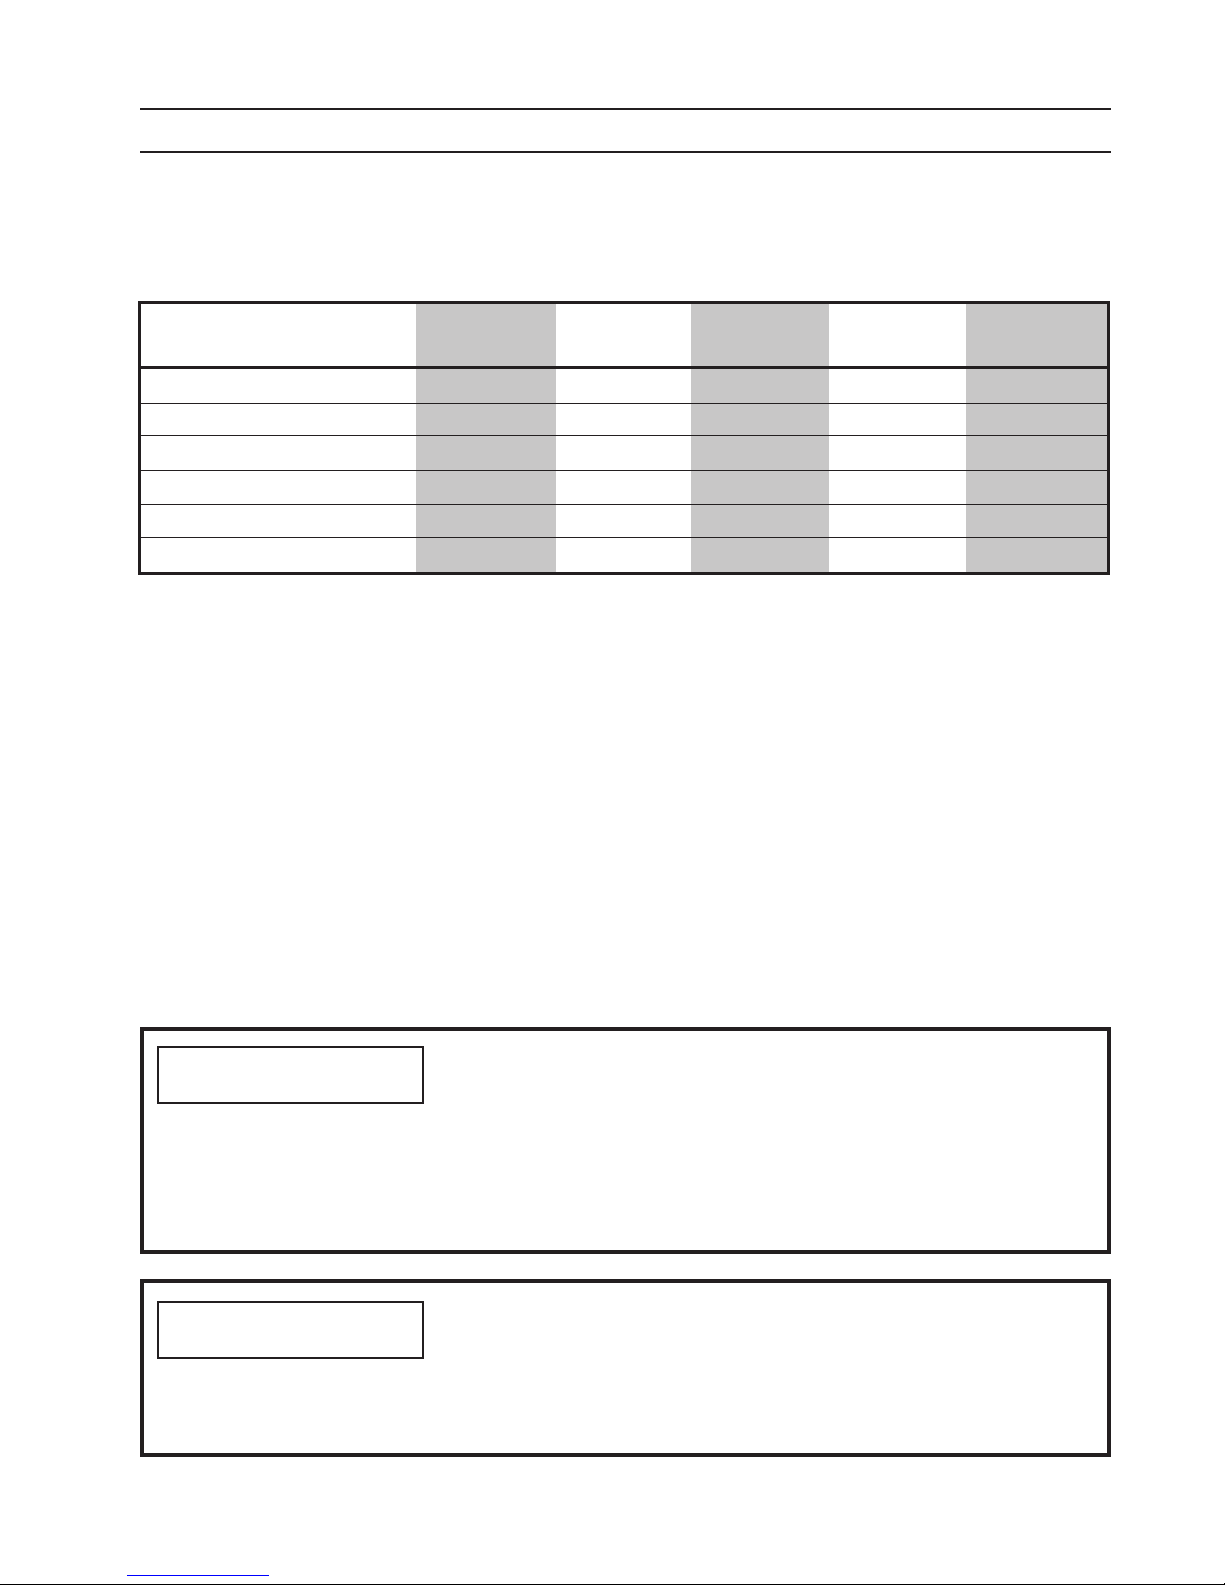
2.5 Gas Hoses
Gas Type 25 ft. 50 ft. 75 ft. 100 ft. 125 ft.
(7.6m) (15.2m) (22.8m) (30.4m) (38.1m)
Nitrogen (clear) 33122 33123 33124 33125 33126
Oxygen (clear - USA) 33117 33118 33119 33120 33121
Oxygen (blue - Euro) 0558002973 0558002974 0558002975 0558002976 0558002977
Argon/Hydrogen (H-35) (1) 33122* 33123* 33124* 33125* 33126*
Air (clear - USA) 33122** 33123** 33124** 33125** 33126**
Air (black - Euro) (2)
Note: * = Requires adapter P/N 19X54 (order separately)
** = Requires adapter P/N 74S76 (order separately)
2.6 Gas Regulators
Nitrogen ....................................... 19155 ............................... 998343
Oxygen.........................................19151 ............................... 998336
Argon/Hydrogen (H-35) ................19153 ...............................998341
Air................................................ 30338 ............................... N/A
NONO
NO
NONO
TICETICE
TICE
TICETICE
0558002978** 0558002979** 0558002980** 0558002981** 0558002982**
Station Regulator Cylinder Regulator
A separate start gas regulator is always required:
• For air plasma use air start gas.
• For oxygen or nitrogen use nitrogen start gas.
• For H-35 (argon/hydrogen) H-35 or nitrogen start gas.
NONO
NO
NONO
TICETICE
TICE
TICETICE
A total of 3 regulators will be required (plasma, start and
secondary).
When using a plumbing box:
• Gas hoses from supply cylinders go directly to the
plumbing box.
• Console gas manifold is not used.
14
Page 15

SECTION 2 DESCRIPTION
2.7 Basic Packages
The EPP-200 system is available as a pre-engineered package
or can be ordered as individual parts as listed.
Basic Packages include:
• EPP-200 Console
• Plasma Torch
• Appropriate regulators for the gases indicated
• Gas hoses from regulators to console
• Torch coolant
Torch Coolant – 1 gallon (3.8 L) P/N 0558004297
15
Page 16

SECTION 2 DESCRIPTION
16
Page 17

SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
3.1 General
WARNINGWARNING
WARNING
WARNINGWARNING
3.2 Unpacking
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
Failure To Follow Instructions Could Lead
To Death, Injury Or Damaged Property
Follow these instructions to prevent injury or property
damage.
You must comply with local, state and national electrical and
safety codes.
CACA
CA
CACA
UTIONUTION
UTION
UTIONUTION
Use Lifting Eye When Hoisting From
Overhead
Use safe practices when transporting with overhead method.
Unit weighs over 700 lbs (318 kg). Use approved straps or
cables in good condition.
• Inspect for transit damage immediately upon receipt.
• Remove all components from shipping container and
check for loose parts in container.
• Inspect louvers for air obstructions.
17
Page 18

SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
CACA
CA
CACA
3.3 Placement
UTIONUTION
UTION
UTIONUTION
Plasma
Console
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
Do Not Restrict Air Flow
Restricting intake air with any type of filter on or around the
Plasma console will result in overheating and may void the
warranty.
• A minimum of 2 ft. (0.61m) clearance for cooling air flow.
• Plan for top panel and side panels having to be removed
for maintenance, cleaning and inspection.
• Locate the EPP-200 relatively close to a properly fused
electrical power supply.
• Keep area beneath power source clear for cooling air
flow.
• Environment should be relatively free of dust, fumes and
excessive heat. These factors will affect cooling
efficiency.
Conductive Dust And Dirt Inside Power
CACA
CA
CACA
3.4 Input Connections to Console
WARNINGWARNING
WARNING
WARNINGWARNING
UTIONUTION
UTION
UTIONUTION
Source May Cause Arc Flash Over
Equipment damage may occur. Electrical shorting may
occur if dust is allowed to buildup inside power source.
See maintenance section.
Electric Shock Can Kill!
Provide maximum protection against electrical shock.
Before any connections are made inside the machine,
open the line wall disconnect switch to turn power off.
18
Page 19

SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
3.4.1 Primary Power Specifications
EPP-200 is a 3-phase unit. Input power must be provided from
a line (wall) disconnect switch that contains fuses or circuit
breakers in accordance to local or state regulations.
Recommended input conductor and line fuse sizes:
Rated Load Input and Time delay
Volts Amperes conductor* (amperes)
200/208 115 1 150
230 100 2 125
380 60 4 80
415 55 6 70
460 50 6 70
575 40 8 60
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
Ground Fuse size
CU/AWG
NONO
NO
NONO
TICETICE
TICE
TICETICE
* Sizes per National Electrical Code for a 75° C (165° F) rated
copper conductors @ 40° C (104° F) ambient. Not more than
four conductors in raceway or cable. Local codes should be
followed if they specify sizes other than those listed above.
Input current values given in this table are at maximum output
power (32kW) 200 amps at 160VDC.
Dedicated power line may be necessary.
EPP-200 is equipped with line voltage compensation but to
avoid impaired performance due to an overloaded circuit,
a dedicated power line may be required.
19
Page 20
SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
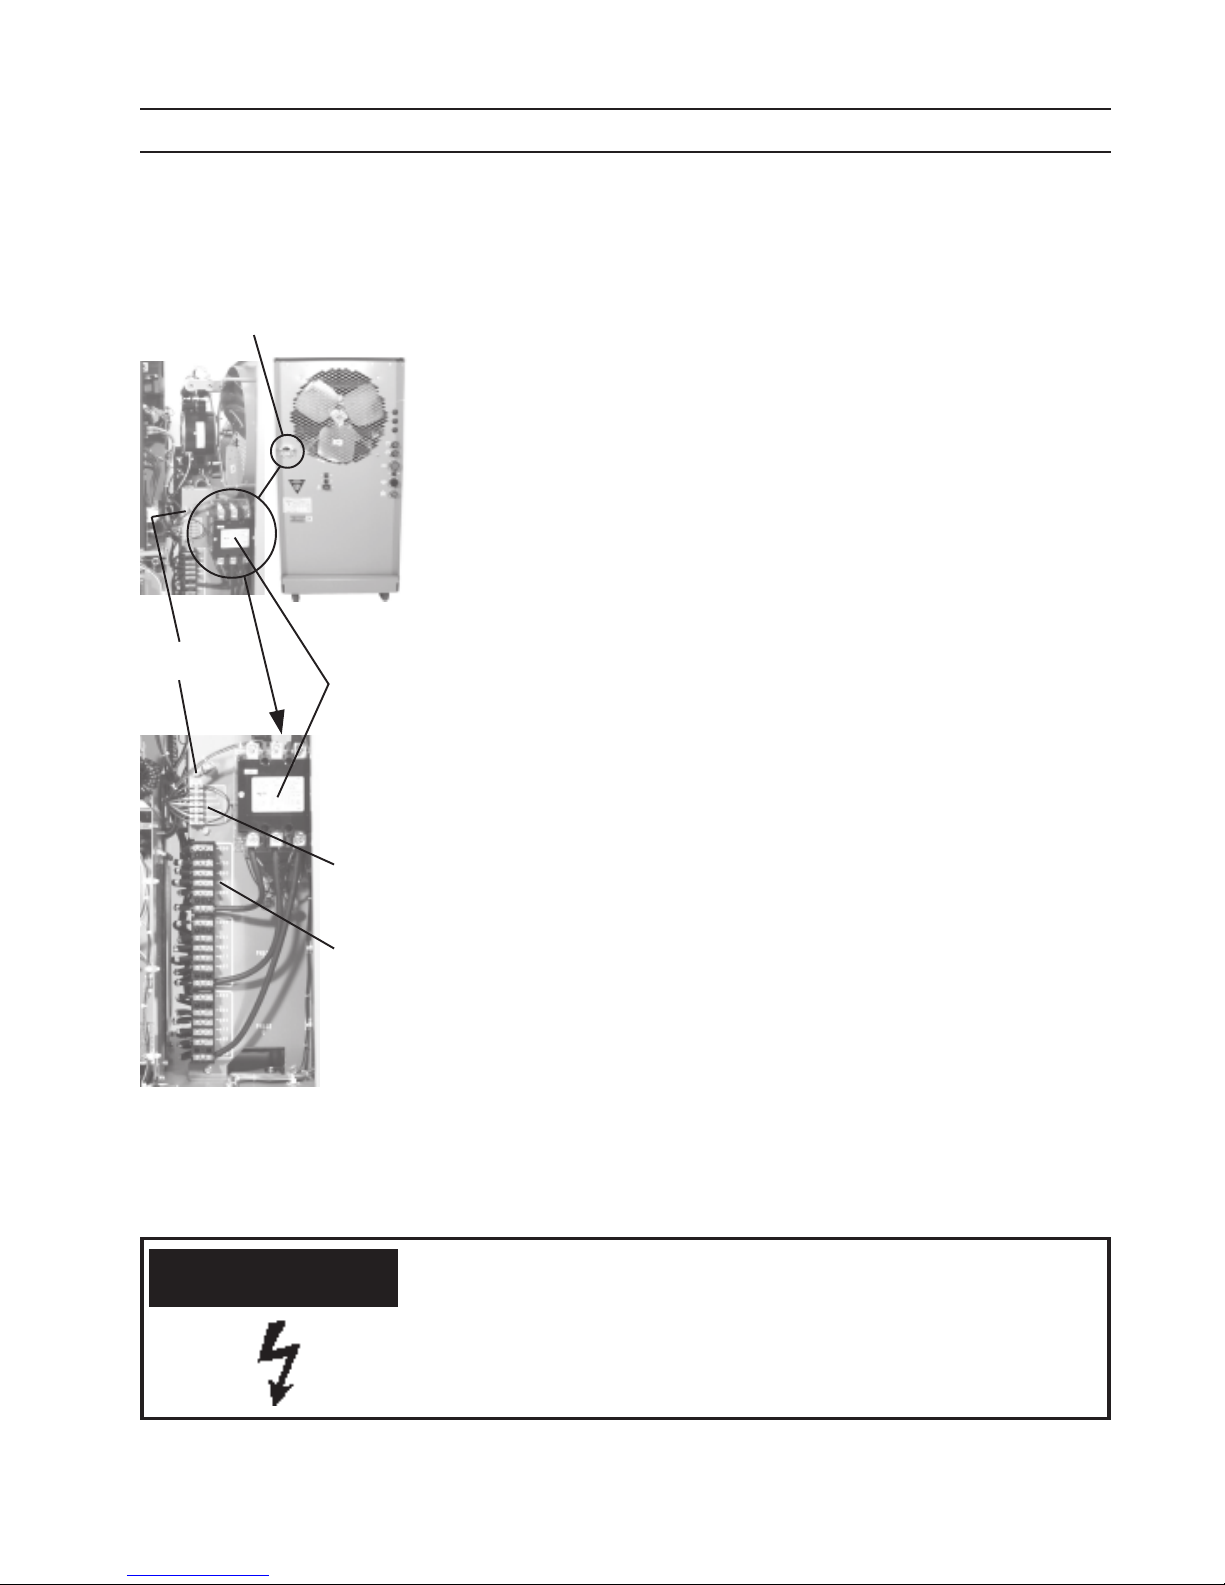
3.4.2 Primary Power Hookup Procedure
The following procedure explains the proper installation steps
Input Power Cable
Strain Relief
for connecting primary electrical power to the plasma console.
NOTE: Safety codes specify the power ground wire be
the last connection to break should the cable be pulled
out of the unit. When preparing the cable for connection,
make the ground wire 6 inches (152mm) longer than the
three pr primary wires.
1. Ensure input power cable is disconnected from all electrical
sources.
2. Remove right side panel (as viewed from front of console).
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
Ground
Connection
Factory wired
for 575 volts
Main
Contactor
7 Position
Terminal
Block
Auto
Transformer
3. Route input power cable through the strain relief located at
the rear panel.
4. Pull input power cable through the strain relief to allow cable
wires sufficient length to connect to main contactor. Tighten
strain relief to ensure input power cable is secured.
5. Connect input power cable ground wire to the ground lug
provided above TB2 (7 position terminal block).
6. Connect three power leads of input power cable to terminals
located atop the main contactor. Secure the leads by tightening
each screw.
7. Connect jumper power cables from bottom of the main
contactor to proper input voltage marked on auto transformer.
Unit is factory set for 575V as shown at the left.
8. Connect jumper on TB2 to proper input voltage. This 7
position terminal block jumper is factory set to 575V.
CACA
CA
CACA
UTIONUTION
UTION
UTIONUTION
Input Power Jumper Connection
Ensure each input power jumper cable is connected to
correct input voltage on autotransformer and on TB2.
Factory wired for 575 Volts
20
Page 21
SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
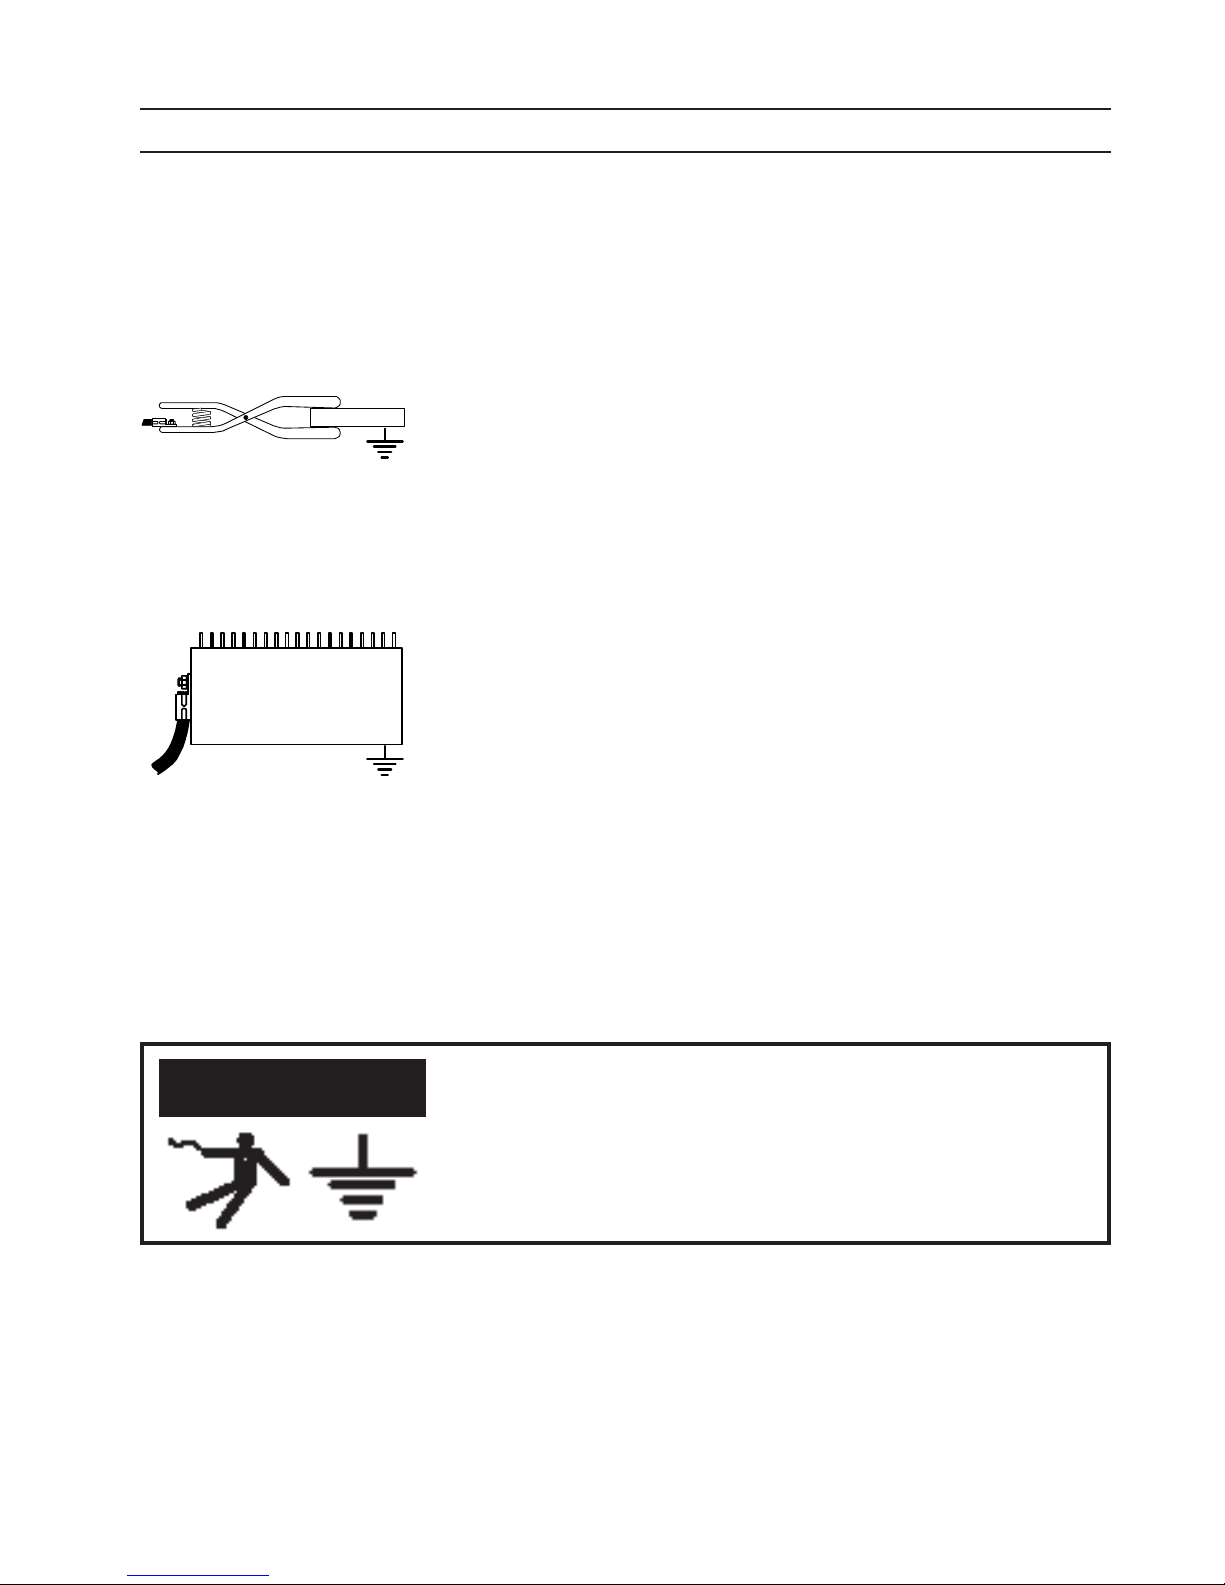
Work ground to work piece
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
9. Connect input conductors to line (wall) disconnect.
10. Replace side panel. Replace only if all connections have
made. Output connections require this panel to be removed.
11. Connect the other end of work cable to workpiece or
cutting table. Connection must be made to a clean, exposed
metal surface, free of paint, rust, mill scale, etc.
Work ground to cutting table
WARNINGWARNING
WARNING
WARNINGWARNING
Electric Current Is Hazardous.
It is important to have a good earth ground connected to
the workpiece or cutting table.
21
Page 22
SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
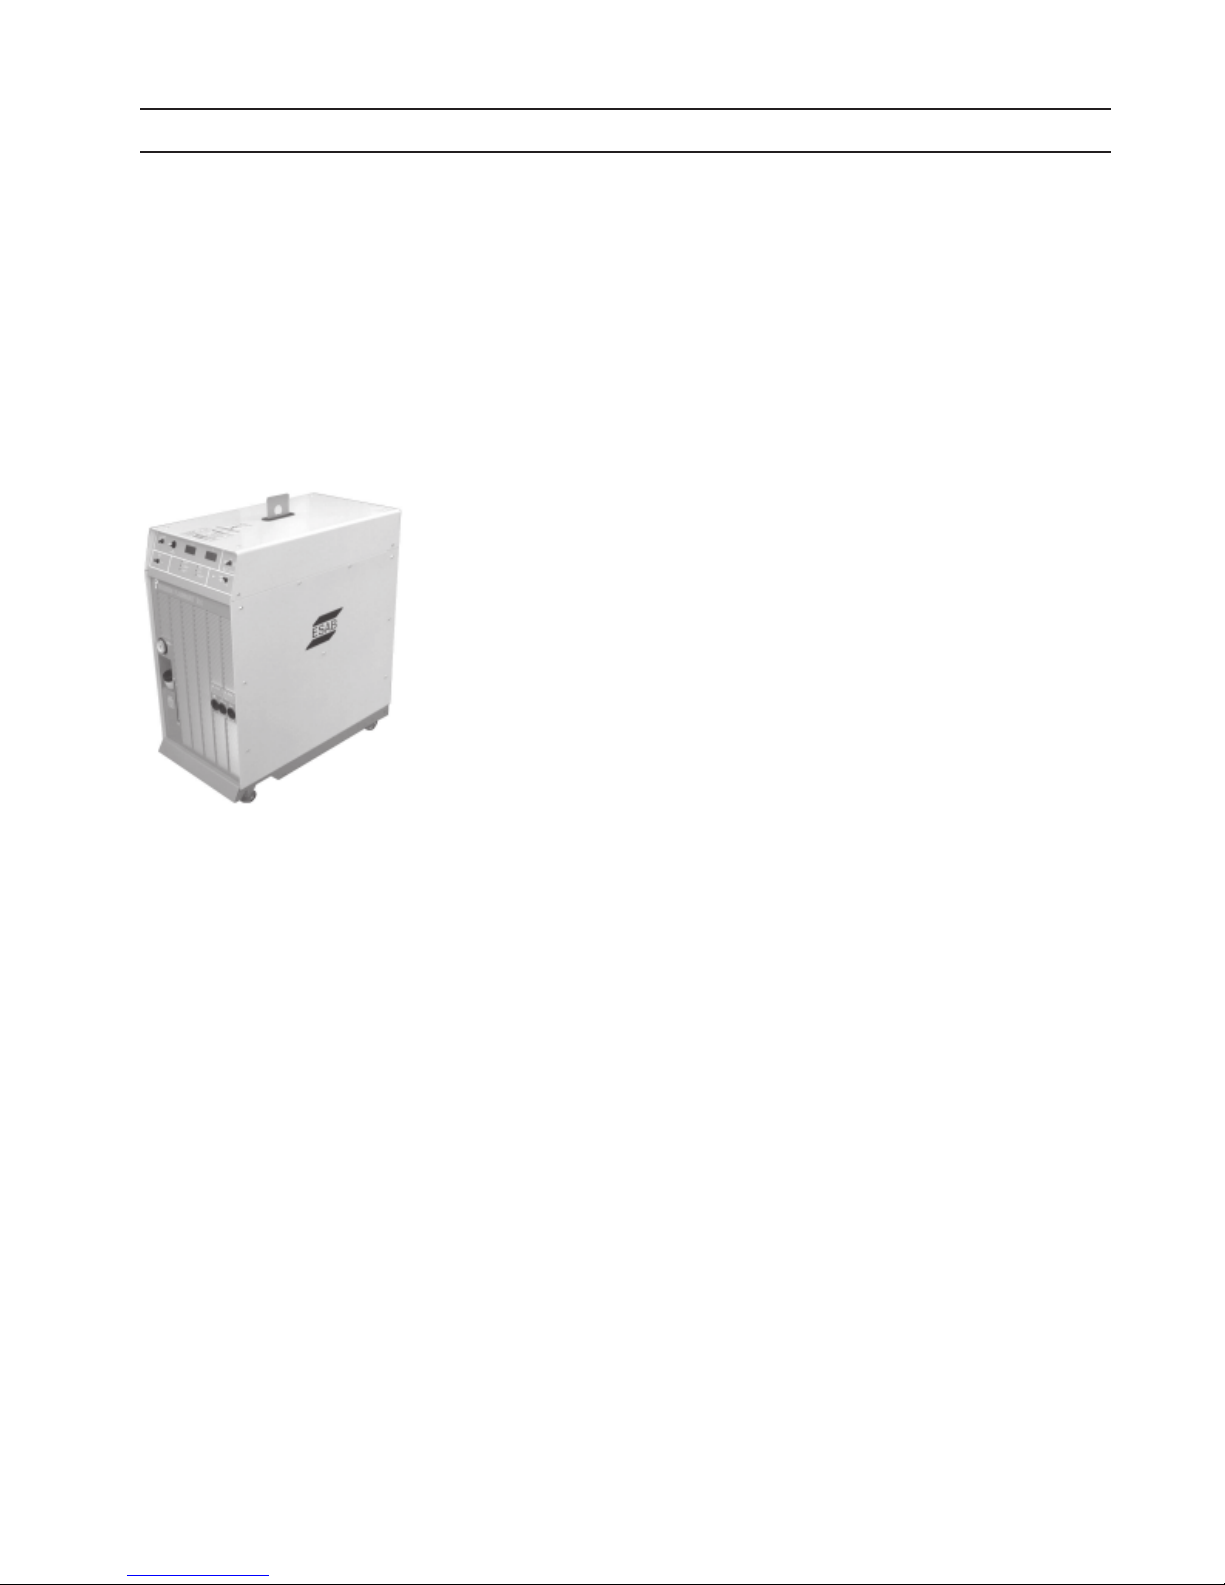
3.5 Connecting Plasma Torches to EPP-200 Console and Options
3.5.1 EPP-200 Output Cables, Hoses and Adapters (customer supplied)
EPP-200:
Lengths vary depending on system.
• Coolant Return
• Coolant Supply
• Pilot Arc Cable
• Electrode Cable
• Shield Gas (directly to the Plumbing Box)
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
• Start Gas (directly to the Plumbing Box)
• Cut Gas (directly to the Plumbing Box)
• Work Cable
• Pendant Cable (if pendant option is ordered)
See Description, Section 2 for part numbers.
A remote SETUP Panel option (P/N 22000) is available on
Avenger 1 and larger ESAB cut cutting machines. This panel
operates the same as the pendant. Refer to your machine
manual for replacement parts.
22
Page 23
SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
3.6 Coolant Installation
WARNINGWARNING
WARNING
WARNINGWARNING
CACA
CA
CACA
UTIONUTION
UTION
UTIONUTION
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
Electric Current Is Hazardous.
It is important to have a good earth ground connected to
the workpiece or cutting table.
Commercial Antifreeze Will Cause Torch To
Malfunction.
Use special torch coolant. P/N 156F05
Due to high electrical conductivity, DO NOT use tap water
or commercial automotive type antifreeze for torch cooling.
A specially formulated torch coolant is REQUIRED. This
coolant also protects from freezing to -34° C (-29° F).
Operating the unit without coolant will cause permanent
damage to the coolant pump.
Check coolant level frequently.
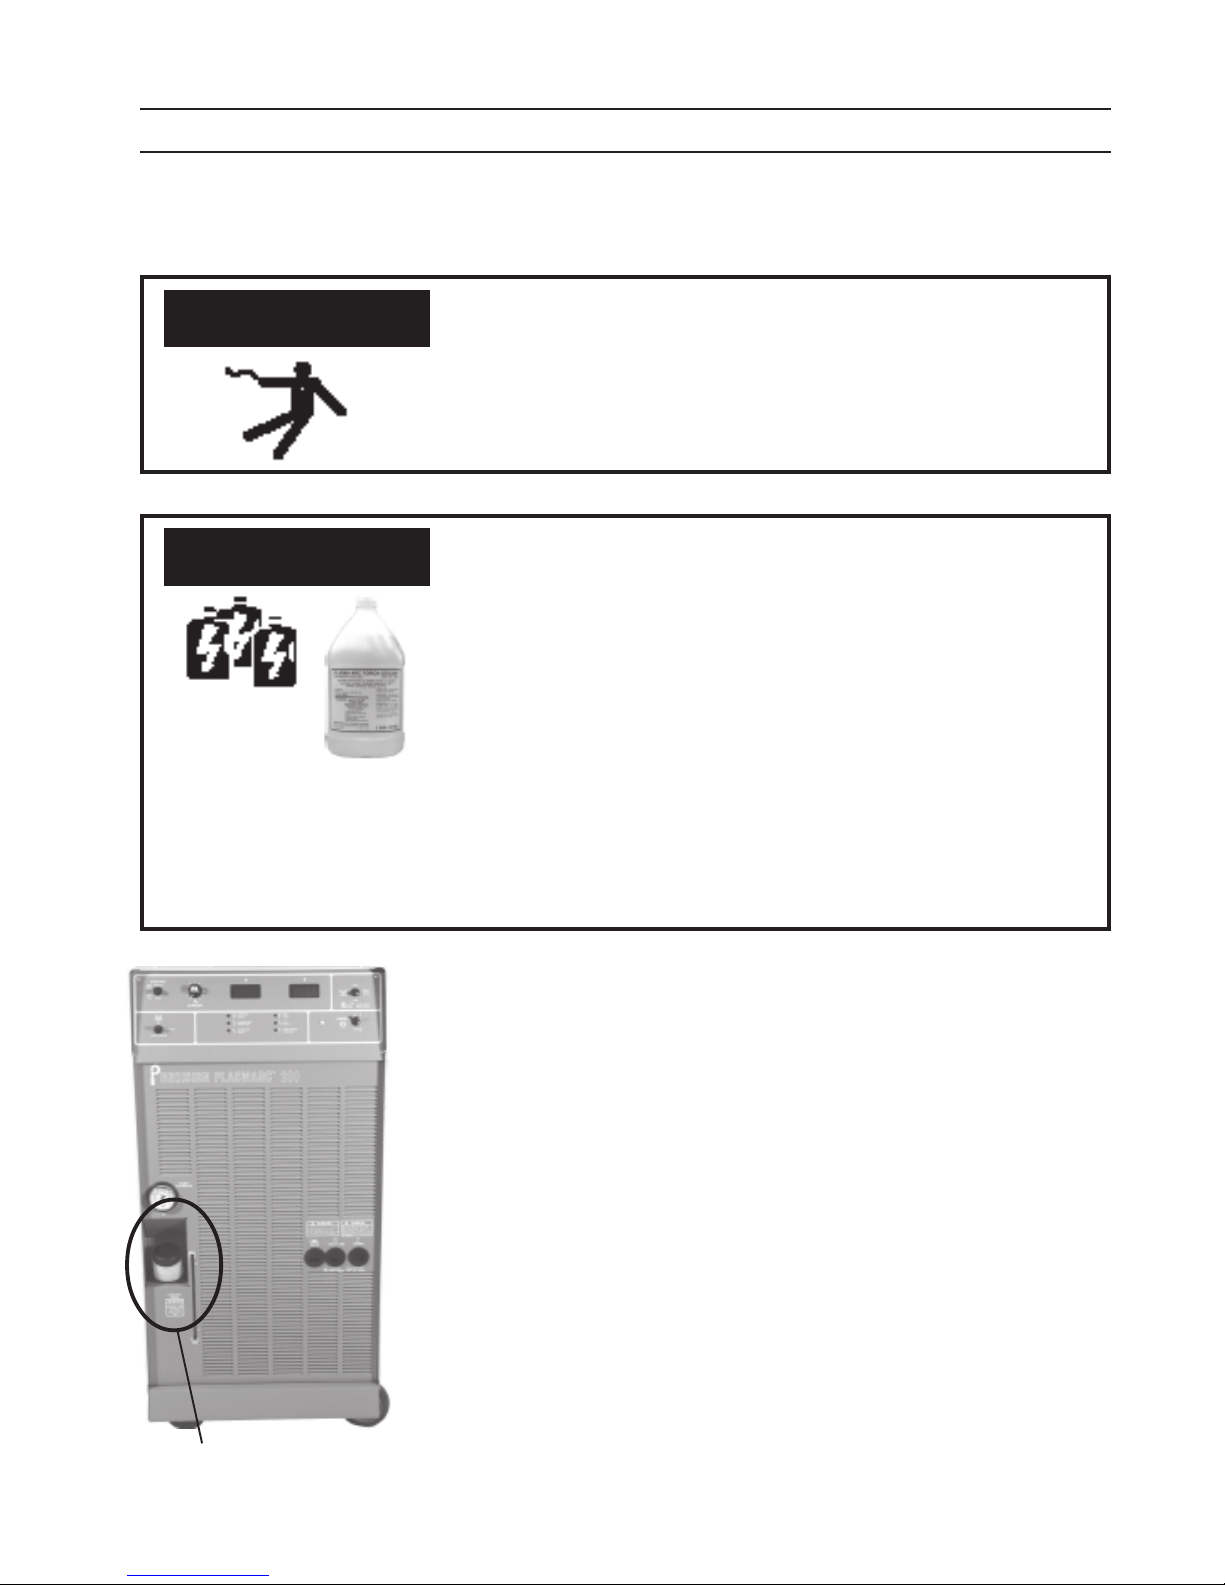
Remove coolant fill cap at front console and fill coolant tank
with 4 gallons (15 liters) of plasma torch coolant, P/N 156F05
(one gallon / 3.8 liters).
• Do not fill above indicated maximum level.
• Reinstall cap.
Coolant Fill Cap
23
Page 24
SECTION 3SECTION 3
SECTION 3
SECTION 3SECTION 3
INSTALLATIONINSTALLATION
INSTALLATION
INSTALLATIONINSTALLATION
24
Page 25
SECTION 4SECTION 4
SECTION 4
SECTION 4SECTION 4
4.1 Introduction – Operational Safety
Electric Shock Can Kill!
DD
ANGERANGER
D
ANGER
DD
ANGERANGER
Disconnect current supply at wall disconnect before
servicing console, torch or plumbing box.
• Do not operate console or plumbing box with any covers
removed/open.
• Do not touch any torch front-end parts with power on.
• Do not attempt to service any portion of this plasma
system unless power has been disconnected at the wall
disconnect.
OPERATIONOPERATION
OPERATION
OPERATIONOPERATION
WARNINGWARNING
WARNING
WARNINGWARNING
WARNINGWARNING
WARNING
WARNINGWARNING
This equipment can be hazardous if not
properly operated and maintained.
Read and understand all equipment literature and warning
labels before operating this equipment.
Plasma Arc Cutting Can Be Hazardous To
Eyes And Ears.
• Wear hearing protection.
• Wear eye protection specifically designed for arc
welding and cutting. Lenses should be at least a No. 6
or No. 7 lens shade.
• Wear protective clothing to avoid skin burns.
25
Page 26
SECTION 4SECTION 4
SECTION 4
SECTION 4SECTION 4
4.2 Operating the EPP-200 Console
4.2.1 Console Controls
OPERATIONOPERATION
OPERATION
OPERATIONOPERATION
4
5
3
2
6
1
7
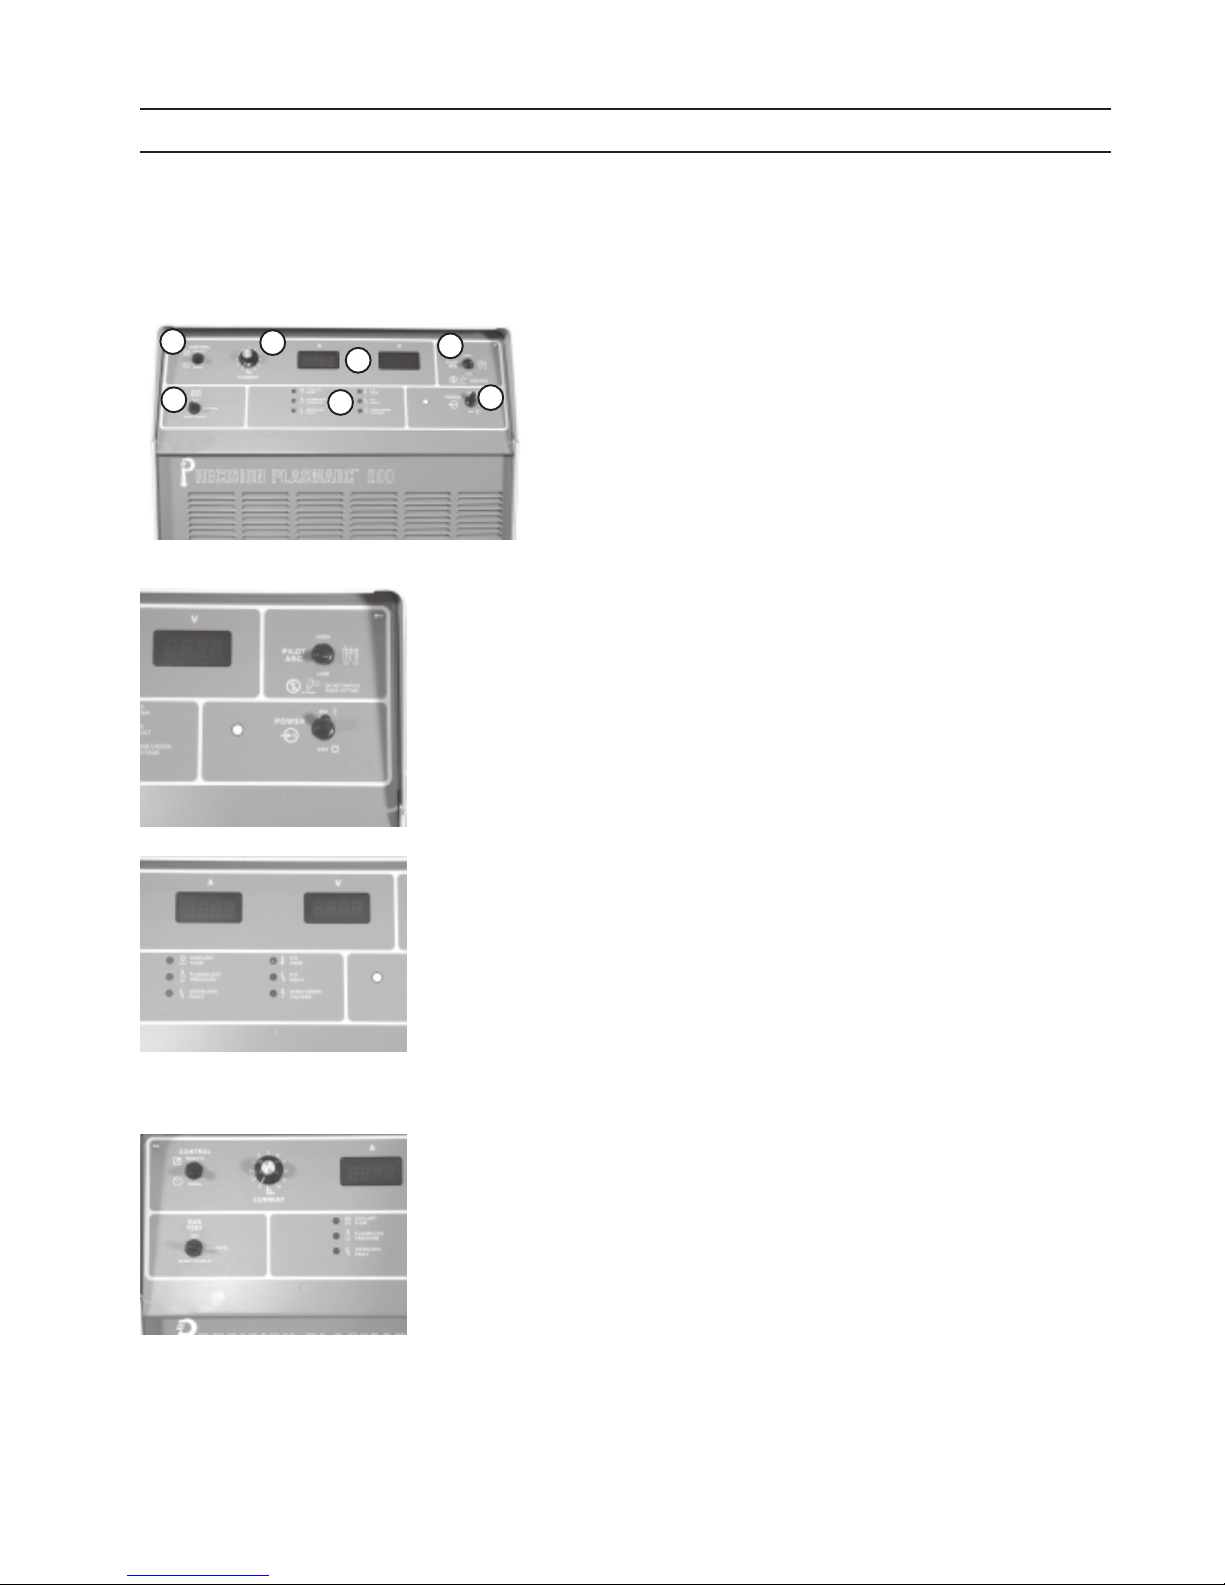
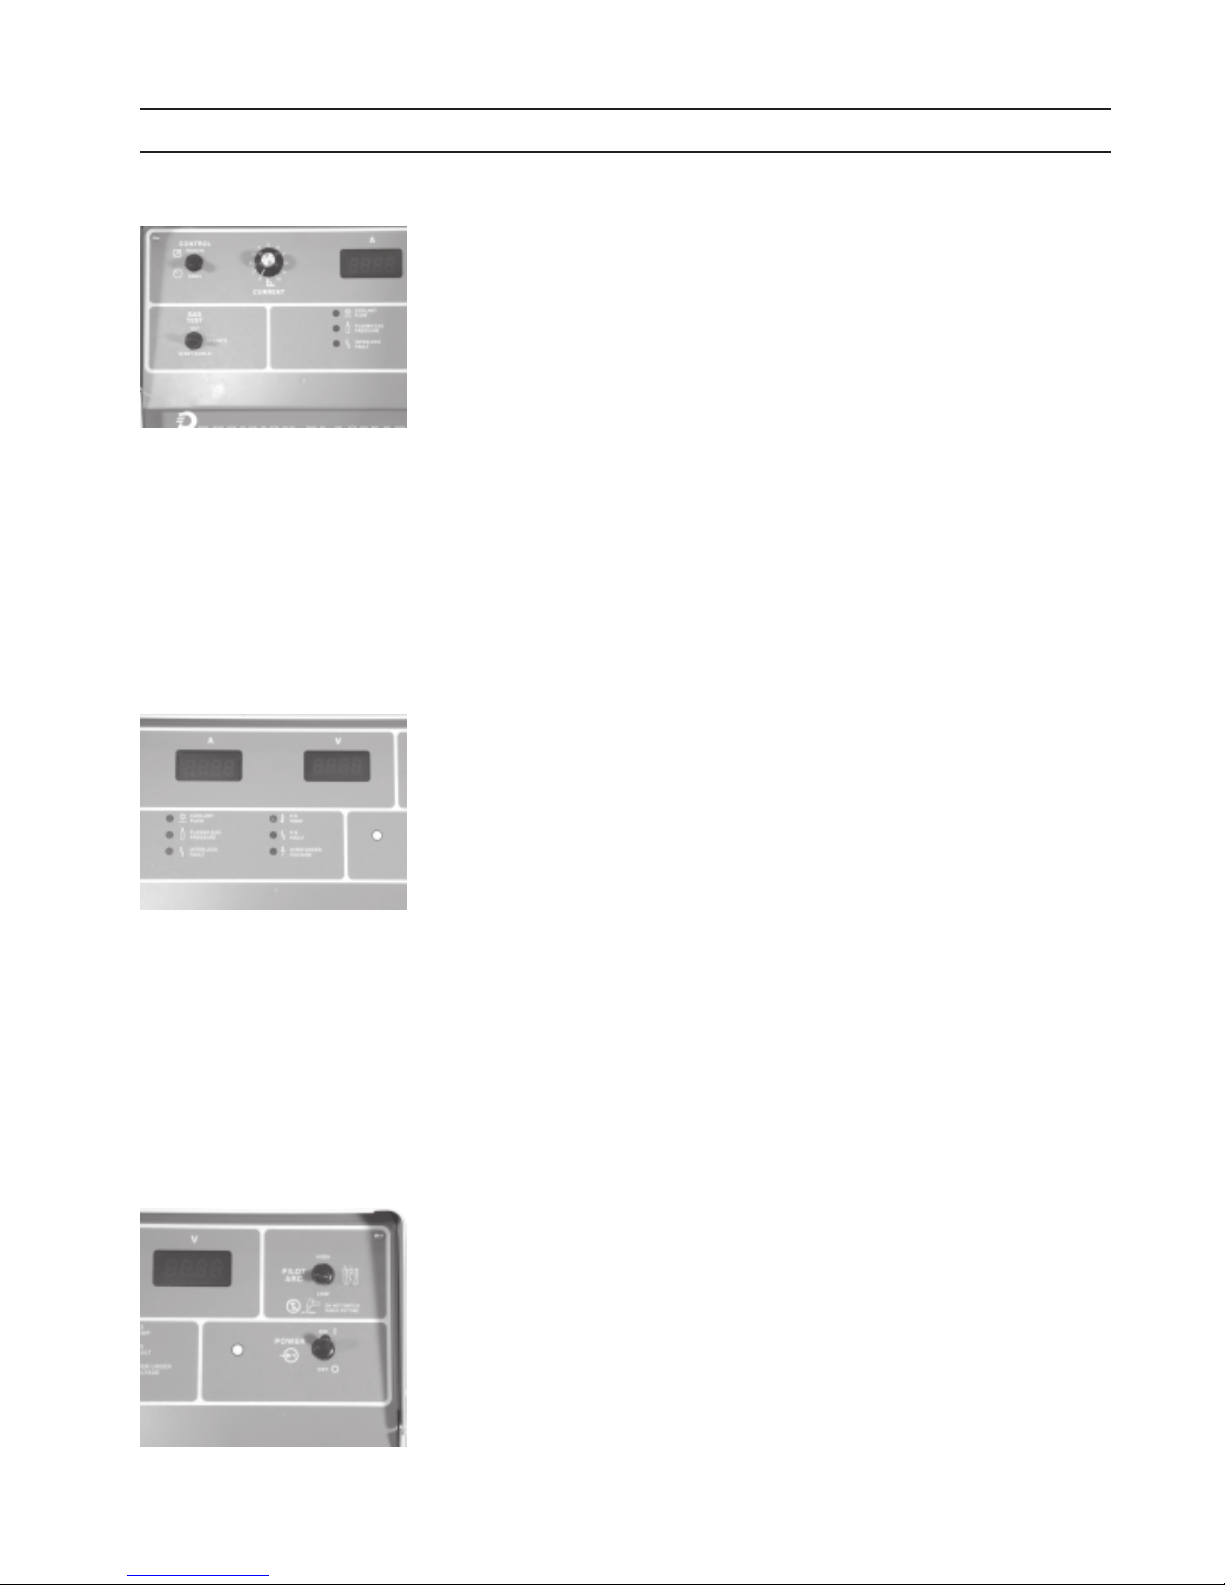
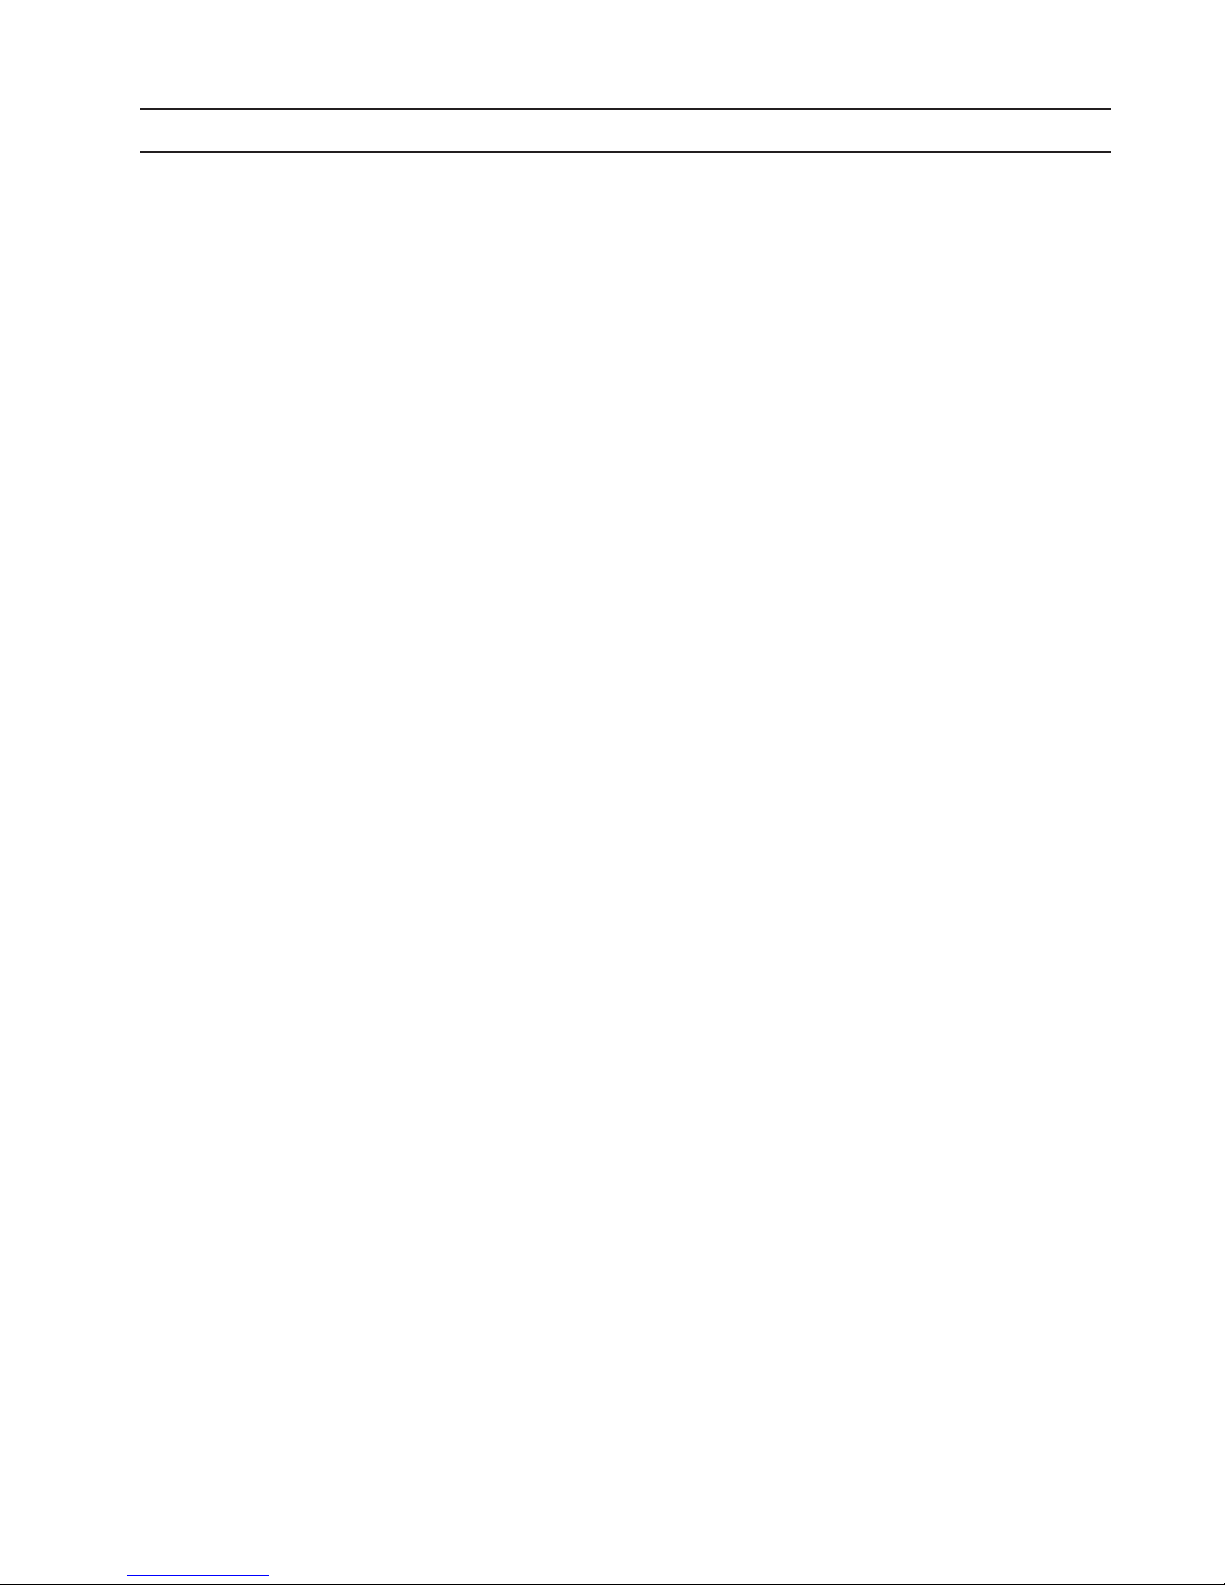
1 Pilot Arc High/Low Switch
2 Cutting Voltage and Cutting Current Meters
3 Output Current Control
4 Remote/Panel Selection Switch
5 Gas Test Switch
6 Fault Lights
7 Main Power Switch
Pilot Arc Switch
Used to select pilot arc current range when Remote / Panel
Switch is in the Panel position. HIGH position is used for most
cutting applications. Electrode life is adversely affected when
used in high position when low is suitable. Starting may be
difficult if set on low when high is required. Related to the initial
torch standoff height.
Cutting Voltage and Current Meters
“A” meter indicates actual cutting current, 0-200 amperes
“V” meter indicates actual output voltage, 0-160 VDC
Output Current Control
Sets the cutting current when current settings are made from
the power console front panel. (The Remote/Panel switch must
be in the Panel position.)
Remote/Panel Switch
Panel position – Output current is set by the output current
control on the console front panel as described above.
Remote position – Output current is set by the CNC with an
analog dc signal.
26
Page 27
SECTION 4SECTION 4
SECTION 4
SECTION 4SECTION 4
OPERATIONOPERATION
OPERATION
OPERATIONOPERATION
Gas Test Switch
Cut – Allows for setup of cut gas pressure and flow. Start/
Shield – Setup of gas pressures and flows.
Operate – Default position – Must be in this position for
cutting.
Fault Indicator Lights
• Coolant Flow – Will show low coolant flow. Light will
briefly show a fault when console is turned on and then
go out.
• Plasma Gas Pressure — fault indicator – low plasma
gas pressure. Torch will not fire when illuminated.
• Interlock Fault – Indicates Remote Plumbing box door
is not properly closed.
• P/S Temp – fault indicator – over temperature condition
in the inverter power source.
• P/S Fault – fault indicator – Not used.
• Over/Under Voltage – fault indicator – input voltage is
above or below tolerances of the power source console.
Will stay shut down console until main power switch is
recycled and fault is corrected.
Main Power Switch
Controls the input power to the fan, water cooler, inverter and
interface circuitry. Light illuminates to indicate power is on.
27
Page 28
SECTION 4SECTION 4
SECTION 4
SECTION 4SECTION 4
4.3 Sequence of Operation
OPERATIONOPERATION
OPERATION
OPERATIONOPERATION
1. Apply power by closing the line (wall) switch. Main power
light will not illuminate until console power switch is turned
ON. Fault light should flash and go out.
2. Select the Panel/Remote setting. If current is controlled
from cutting machine CNC, place switch to Remote position.
Consult cutting machine instructions for current setting. If
current is not controlled by the CNC, select Panel and set
current on output current dial.
3. Check coolant level. Level must be checked with console
main power in OFF position. Coolant level must fall in the
safe operating level.
4. Set pilot arc High/Low switch. Refer to cutting process data
of the torch manual.
5.Turn on console power by placing power switch in ON position.
White light to left of the switch will illuminate.
6. Check coolant pressure. The pressure is factory set between
80 to 90 PSI (5.5-6.2 bars)
7. Begin plasma cutting operation. This may include manually
setting other options, depending on total plasma package.
If using panel mode, after cutting has begun, adjust current to
desired amount.
Check for a fault light. If a fault light illuminates, SHUT OFF
POWER IMMEDIATELY and refer to troubleshooting section.
28
Page 29
SECTION 5 MAINTENANCE
5.1 General
Electric Shock Can Kill!
WARNING
Open wall disconnect switch before attempting any maintenance
on:
• plasmaconsole
• interconnectingcables
Only trained personnel should perform maintenance or repairs
CAUTION
on this equipment.
5.2 Inspection and Cleaning
Frequent inspection and cleaning of the EPP-200 and related equipment
are recommended for safety and proper operation. Consider the
following during inspection and cleaning:
• Checkworkcabletoworkpiececonnection.
• Checksafetyearthgroundatworkpieceandatpower
source chassis.
• Ensurecableandhosesarenotdamagedor
kinked.
• Ensureallplugs,ttings,andgroundconnectionsare
tight.
• Checkscreenlterincoolantpump(locatedinside
console) periodically and ush as required.
29
Page 30
SECTION 5 MAINTENANCE
Flying Debris Hazard.
WARNING
Flying Debris Can Seriously Injure Eyes
Wear protective eyewear when cleaning with compressed air.
Use low pressure air only.
Avoid Potential Equipment Damage
CAUTION
Water and/or oil can accumulate in compressed air lines. Be sure
todirecttherstairblastawayfromequipmenttoavoid
damaging the junction box or ow control box.
• Withallinputpowerdisconnectedandwithpropereye
andfaceprotection,blowouttheinsideofthepower
source,owcontrol,andjunctionboxusinglow-pressure,
clean dry compressed air.
• Periodicallybleedallwaterfromtheairlter/regulator
trap.
30
Page 31
SECTION 5 MAINTENANCE
5.3 Gas Manifold Pressure Switches
Newer EPP-200 consoles are equipped with nonadjustable preset gas
manifold pressure switches.
Older ESP-200 consoles have adjustable pressure switches.
Both type switches are preset for:
• 17psig(1.2bar),shieldandstartgasswitches
• 22psig(1.5bar),cutgasswitch
5.3.1 Pressure Switch Adjustment Procedure
1. Turn main power switch OFF OFF.
2. Remove right side panel
3. Turn wheel:
•Counterclockwisetoincrease pressure
•Clockwisetodecrease pressure
4. Replace panel.
5. Resumeoperation.
5.3.2 Gas Manifold with Non-adjustable Pressure Switches (reference)
31
Page 32
SECTION 5 MAINTENANCE
32
Page 33
SECTION 6 TROUBLESHOOTING
6.1 Introduction
Electric Shock Can Kill!
WARNING
Ensure all primary power to machine has been externally
disconnected.
Openline(wall)switchbeforeattemptinginspectionorperforming
workinsidetheplasmaconsoleorplumbingbox.
Capacitors Can Store High Voltages.
WARNING
Disconnecting plasma console does not ensure capacitors are deenergized.
Ensure console capacitors are grounded after removing power and
prior to performing maintenance.
6.2 Procedure
1. Shut main power switch on the console to OFF position.
2.Disconnectmainpowerline(wall)switch.
3. Check for obvious external settings, switches and external
connections.
4.Ifaproblemisfound,correctandproceedwithnormaloperations.
5.Ifnot,removesidepanels.(Reminder: Power must be disconnected
before removing any covers.)
6.Performavisualinspectionofinternalcomponents.Checkfor:
• Looseorburnedwiringandcomponents
• Secureterminalconnections
• Bulgedorleakingcapacitors
• Othersignsofdiscoloration
Refer to the troubleshooting guide for identication of many
problems, possible causes and remedies.
Reference wiring diagrams and schematics are found in the last
part of this section
.
33
Page 34
SECTION 6 TROUBLESHOOTING
6.3 Front Panel Fault Lights
Fault Indicator Lights
• Coolant Flow – Will show low coolant ow. The
light will briey show a fault when console is turned on
and then go out.
• Plasma Gas Pressure — fault indicator – low plasma
gaspressure.Torchwillnotrewhenindicated.
• Interlock Fault – Indicates Remote Plumbing box door
is not properly closed.
• P/S Temp – fault indicator – over temperature condition
in the inverter power source.
• P/S Fault – Not used.
• Over/Under Voltage – fault indicator – input voltage is
above or below the tolerances of the power source
console. Will stay shut down console until main power
switch is recycled.
34
Page 35
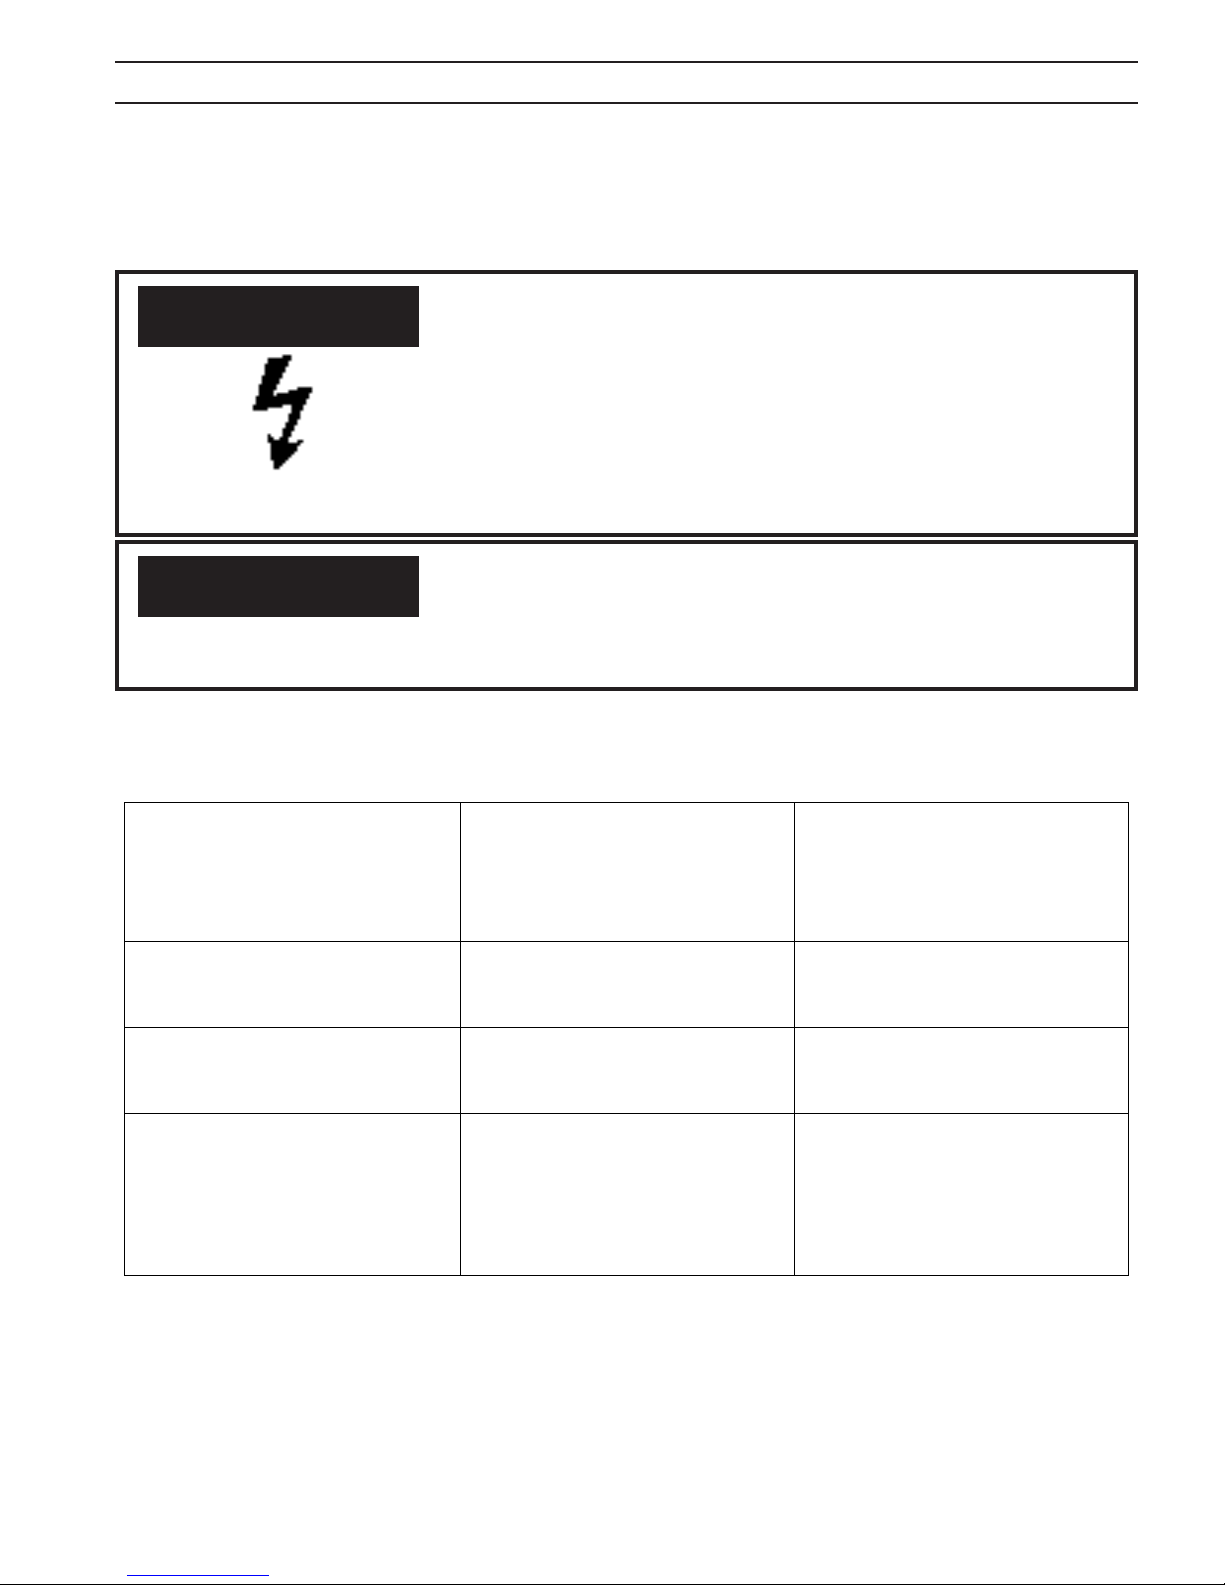
SECTION 6 Troubleshooting
6.4 Troubleshooting Guide
WARNING
!
High Voltages Can Cause Serious
Injury or Death!
Voltages in plasma cutting equipment are high
enough to cause serious injury or death.
Only trained technicians should attempt
diagnosis and repair of this machinery.
CAUTION
!
Avoid damaging your voltmeter.
Disconnect the power from the high frequency
generator before checking voltages in the high
frequency circuit.
Problem
ProblemProblem
Problem Possi
PossiPossi
Possible Cause
ble Causeble Cause
ble Cause Corrective Action
Corrective ActionCorrective Action
Corrective Action
Power switch is ON. Power LED
Power switch is ON. Power LED Power switch is ON. Power LED
Power switch is ON. Power LED
is OFF. Fan is OFF. Pump is
is OFF. Fan is OFF. Pump is is OFF. Fan is OFF. Pump is
is OFF. Fan is OFF. Pump is
OFF.
OFF.OFF.
OFF.
1) Bad Power switch S1.
2) Open Fuse F4.
3) Open Jumper at TB2.
1) Check continuity of power
switch.
2) Check Fuse F4 and related
wiring
3) Check jumper and wiring of TB2
Power
Power Power
Power switch is ON. Power LED
switch is ON. Power LED switch is ON. Power LED
switch is ON. Power LED
in ON. Pump is OFF. Fan is ON.
in ON. Pump is OFF. Fan is ON.in ON. Pump is OFF. Fan is ON.
in ON. Pump is OFF. Fan is ON.
1) Bad or open CB2.
2) Pump Motor Failed.
1) Reset CB2. Check wiring and
check free rotation of pump fan.
2) Replace Pump motor
Power LED is OFF. Pump is ON.
Power LED is OFF. Pump is ON. Power LED is OFF. Pump is ON.
Power LED is OFF. Pump is ON.
Fan is ON. LEDs in power
Fan is ON. LEDs in power Fan is ON. LEDs in power
Fan is ON. LEDs in power
modules are OFF
modules are OFFmodules are OFF
modules are OFF
1) Bad or Open CB1. 1) a. Reset CB1
b. If CB1 fails to reset, check
wiring, bad T1, or PCB1.
Plasma gas fault indicator is ON
Plasma gas fault indicator is ONPlasma gas fault indicator is ON
Plasma gas fault indicator is ON
1) Plasma gas pressure to console
is below 40 psi.
2) Bad pressure switch
3) Open wire between pressure
switch and PCB1.
1) Adjust gas pressure to proper
level for torch and application
2) Adjust (if adjustable type) or
replace pressure switch.
3) Check wiring between PS1 &
PS2 and PCB1 P1-9 and P1-10.
SECTION 6 TROUBLESHOOTING
6.4 Troubleshooting Guide
High Voltages Can Cause Serious Injury or Death!
WARNING
Voltages in plasma cutting equipment are high enough to cause
serious injury or death.
Only trained technicians should attempt diagnosis and repair of
this machinery.
CAUTION
Avoid damaging your voltmeter.
Disconnect the power from the high frequency generator before
checkingvoltagesinthehighfrequencycircuit.
35
Page 36
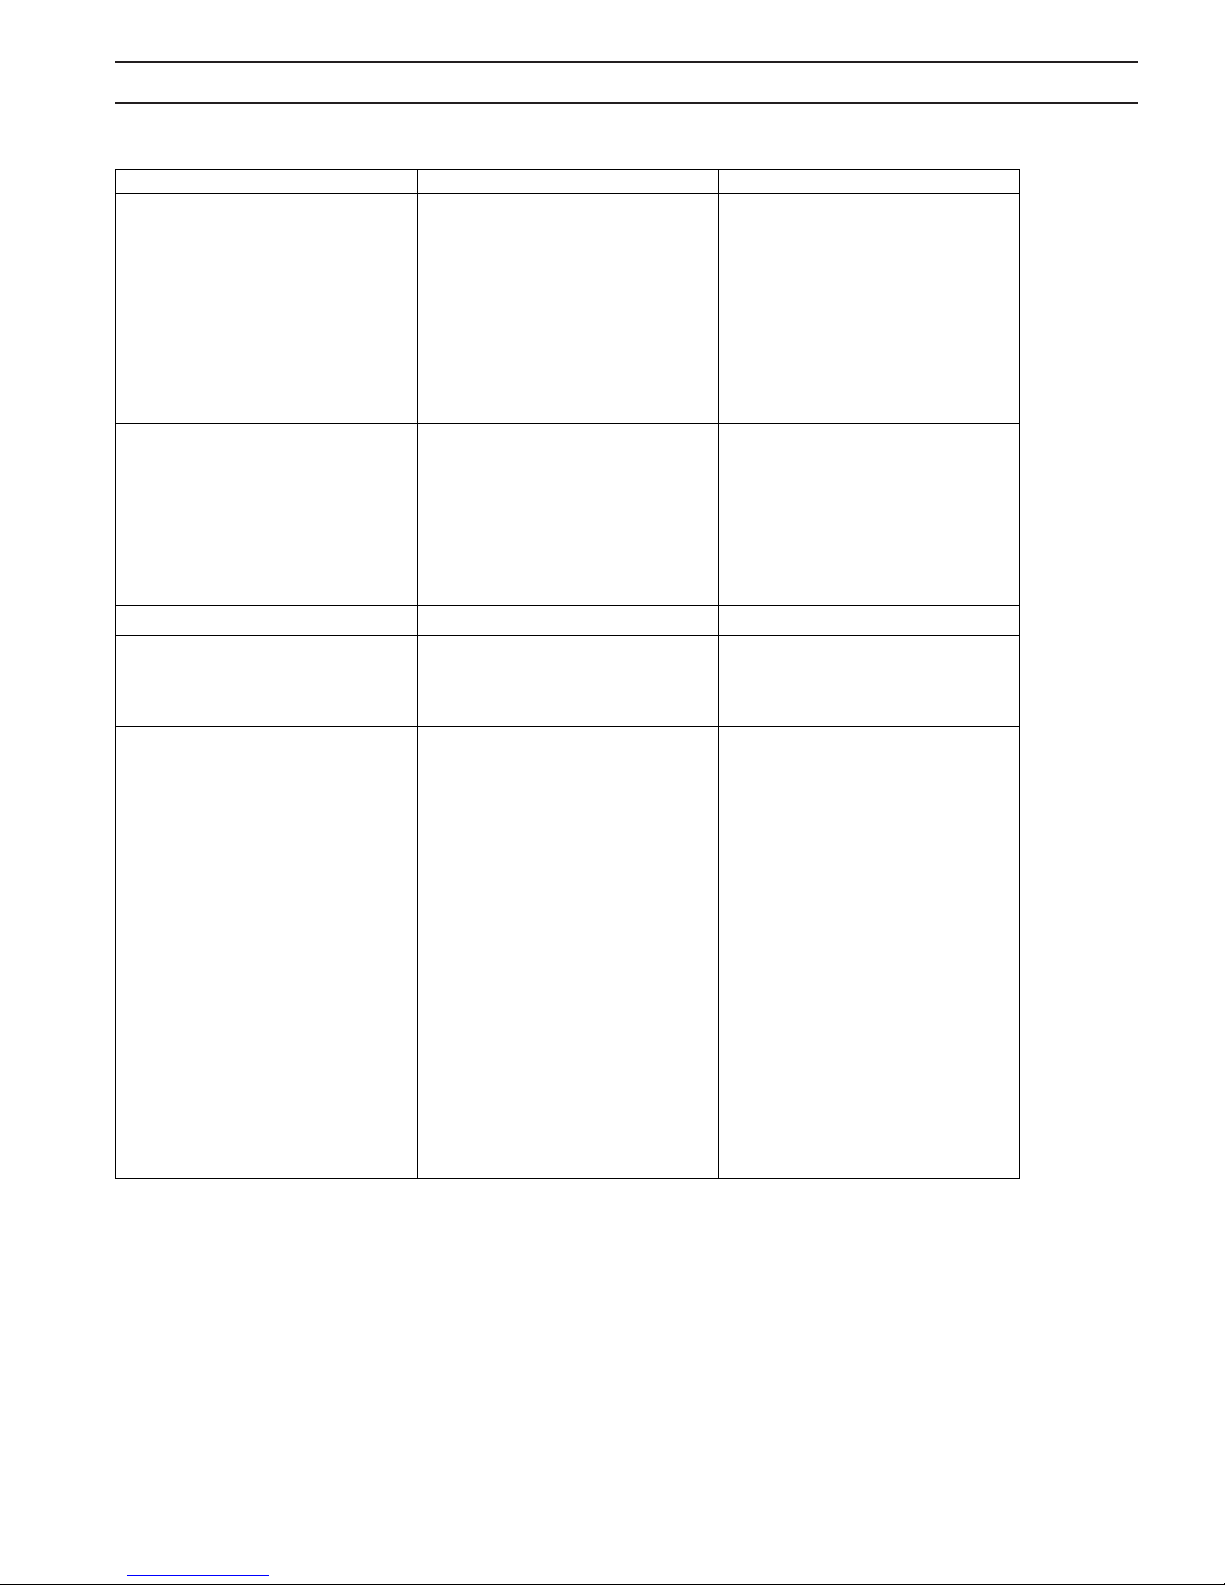
SECTION 6 Troubleshooting
Problem
ProblemProblem
Problem Possible Cause
Possible CausePossible Cause
Possible Cause Corrective Action
Corrective ActionCorrective Action
Corrective Action
Power Source Temp fault
Power Source Temp fault Power Source Temp fault
Power Source Temp fault
indicator is ON.
indicator is ON.indicator is ON.
indicator is ON.
1) Poor ventilation at rear of
console.
2) Open thermal switch.
3) Open wire between temperature
switch and PCB1
1) Make sure that there is 2 feet of
clearance on each side of
console.
2) With power OFF, check each
thermal switch. Normal
operation is: switch closed
below 194
F.
3) Check wiring between
temperature switches and PCB1
P1-15 and P1-16.
Over/Under Voltage fault indicator
Over/Under Voltage fault indicator Over/Under Voltage fault indicator
Over/Under Voltage fault indicator
is ON
is ONis ON
is ON
1) Input voltage is 15% above or
below the selected console
operating voltage.
2) Bad PCB1.
3) Bad PCB1 in MOD1.
4) Bad T1 in MOD1.
1) Provided input voltage must be
equal to the selected console
operating voltage. Change if
necessary.
2) Replace PCB1.
3) Replace PCB1 in MOD1
4) Replace T1 in MOD1
Meters M1 or M2, no display.
Meters M1 or M2, no display.Meters M1 or M2, no display.
Meters M1 or M2, no display.
1) Bad Meter 1) Replace Meter meters M
Meters M1 & M2, no display. 1) Bad PCB1.
1) Replace one meter to verify
above step did not happen
twice. If still not working replace
PCB1.
Press torch switch or send start
Press torch switch or send start Press torch switch or send start
Press torch switch or send start
signal.
signal. signal.
signal.
(No pilot arc or main arc transfer.)
(No pilot arc or main arc transfer.)(No pilot arc or main arc transfer.)
(No pilot arc or main arc transfer.)
1) Gas Test switch is in
START/SHIELD or CUT
positions
2) Plasma gas pressure is to LOW
3) Improper current command
signal
4) LEDX on MOD1 PCB1 is not ON
when torch switch is depressed
or start signal sent.
5) LEDX is ON but main contactor
does not close
6) LEDX is ON. Main contactor is
closed. No OCV or arc transfer.
1) Place Gas Test switch in
OPERATE position.
2) Set plasma gas pressure per
torch or application requirements
(above 40 psi)
3) IF in manual mode, panel switch
must be in PANEL and P5 must
be in J5 connector. If in
mechanized mode, panel switch
must be in REMOTE and a
current signal above 0 volts must
be present. P5 must be in J6
connector
4) Test tbd
5) Test tbd
6) Test tbd
SECTION 6 TROUBLESHOOTING
36
Page 37
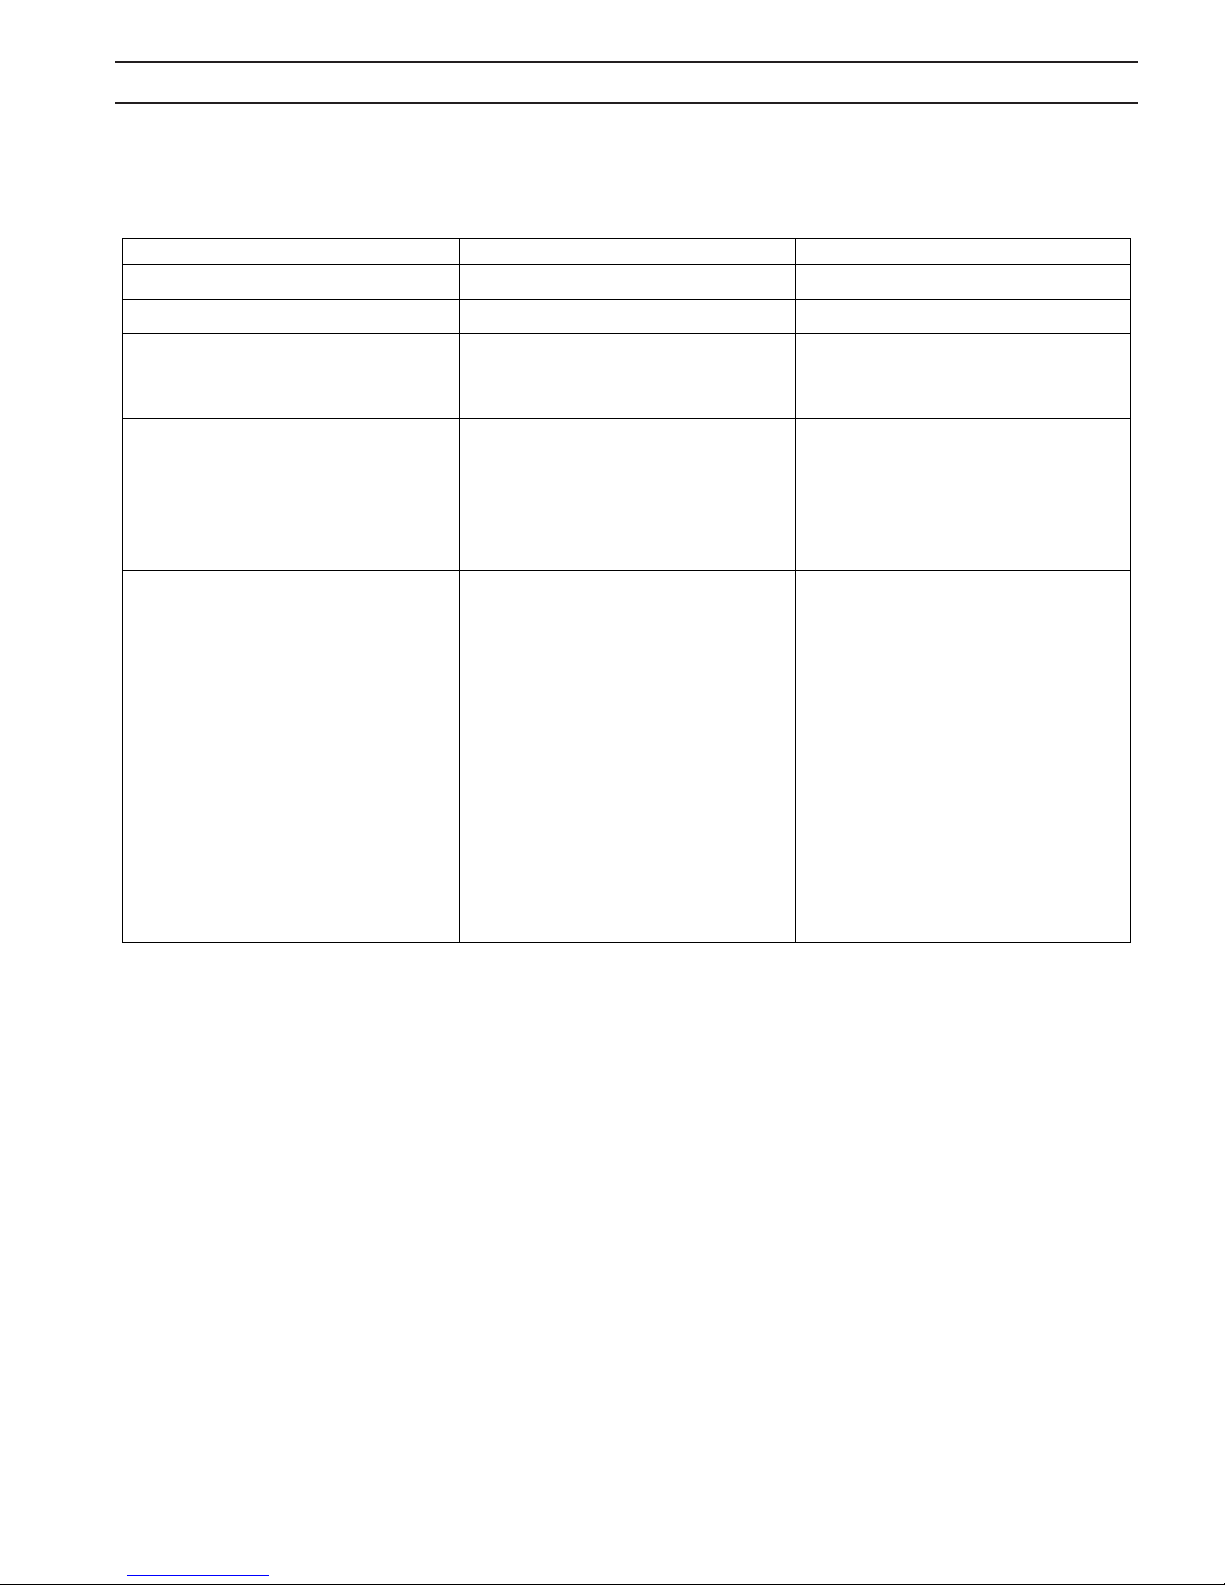
SECTION 6 Troubleshooting
Problem
ProblemProblem
Problem Possible Cause
Possible CausePossible Cause
Possible Cause Corrective Action
Corrective ActionCorrective Action
Corrective Action
LEDX on MOD1 not ON
LEDX on MOD1 not ONLEDX on MOD1 not ON
LEDX on MOD1 not ON
LEDX on MOD2 not ON
LEDX on MOD2 not ONLEDX on MOD2 not ON
LEDX on MOD2 not ON
LEDX on MOD2 not ON when
LEDX on MOD2 not ON when LEDX on MOD2 not ON when
LEDX on MOD2 not ON when
torch switch is depressed or start
torch switch is depressed or start torch switch is depressed or start
torch switch is depressed or start
signal is sent
signal is sentsignal is sent
signal is sent
Arc does not transfer to work.
Arc does not transfer to work.Arc does not transfer to work.
Arc does not transfer to work.
(Ope
(Ope(Ope
(Open Circuit Voltage is between
n Circuit Voltage is between n Circuit Voltage is between
n Circuit Voltage is between
315 and 355. Pilot arc IS
315 and 355. Pilot arc IS 315 and 355. Pilot arc IS
315 and 355. Pilot arc IS
present.)
present.)present.)
present.)
1) Open connection between the
console WORK connector and the
workpiece.
1) a) Check continuity of WORK
cable and clamp
b) Attach clamp to workpiece
c) Ground work table to earth
ground
Arc do
Arc doArc do
Arc does not transfer to work.
es not transfer to work.es not transfer to work.
es not transfer to work.
(Open Circuit Voltage is between
(Open Circuit Voltage is between (Open Circuit Voltage is between
(Open Circuit Voltage is between
315 and 355. Pilot arc is NOT
315 and 355. Pilot arc is NOT 315 and 355. Pilot arc is NOT
315 and 355. Pilot arc is NOT
present.)
present.)present.)
present.)
1) Pilot arc fuses F1 and/or F2 are
open.
2) Bad pilot arc contactor.
3) Bad K3.
4) Bad PCB1 in MOD2.
5) Nozzle to Electrode short in
torch.
6) Bad control PCB
7) No preflow signal from CNC.
8) Current setting to low
9) Contaminated or worn electrode.
1) Replace F1 and/or F2.
2) Replace pilot arc contactor.
3) Replace K3
4) Replace PCB1 in MOD2.
5) Disconnect torch from console.
Check for open between pilot
arc and torch leads. Repair if
shorted.
6) Replace control PCB.
7) Bad PCB1. Bad MOD1 PCB1.
8) Readjust Current setting. Torch
to high above workpiece.
9) Replace electrode.
SECTION 6 TROUBLESHOOTING
SchematicsandWiringDiagramson11"x17"paperareincluded
NOTE:
insidethebackcoverofthismanual.
37
Page 38
SECTION 6 TROUBLESHOOTING
38
Page 39
SECTION 7 REPLACEMENT PARTS
7.1 General
Always provide the serial number of the unit on which the parts will
be used. The serial number is stamped on the unit nameplate.
7.2 Ordering
Toensureproperoperation,itisrecommendedthatonlygenuineESAB
parts and products be used with this equipment. The use of non-ESAB
parts may void your warranty.
Replacement parts may be ordered from your ESAB Distributor.
Note:
Be sure to indicate any special shipping instructions when ordering
replacement parts.
RefertotheCommunicationsGuidelocatedonthebackpageofthis
manual for a list of customer service phone numbers.
Billofmaterialitemsthathaveblankpartnumbersareprovidedfor
customer information only. Hardware items should be available
through local sources.
39
Page 40
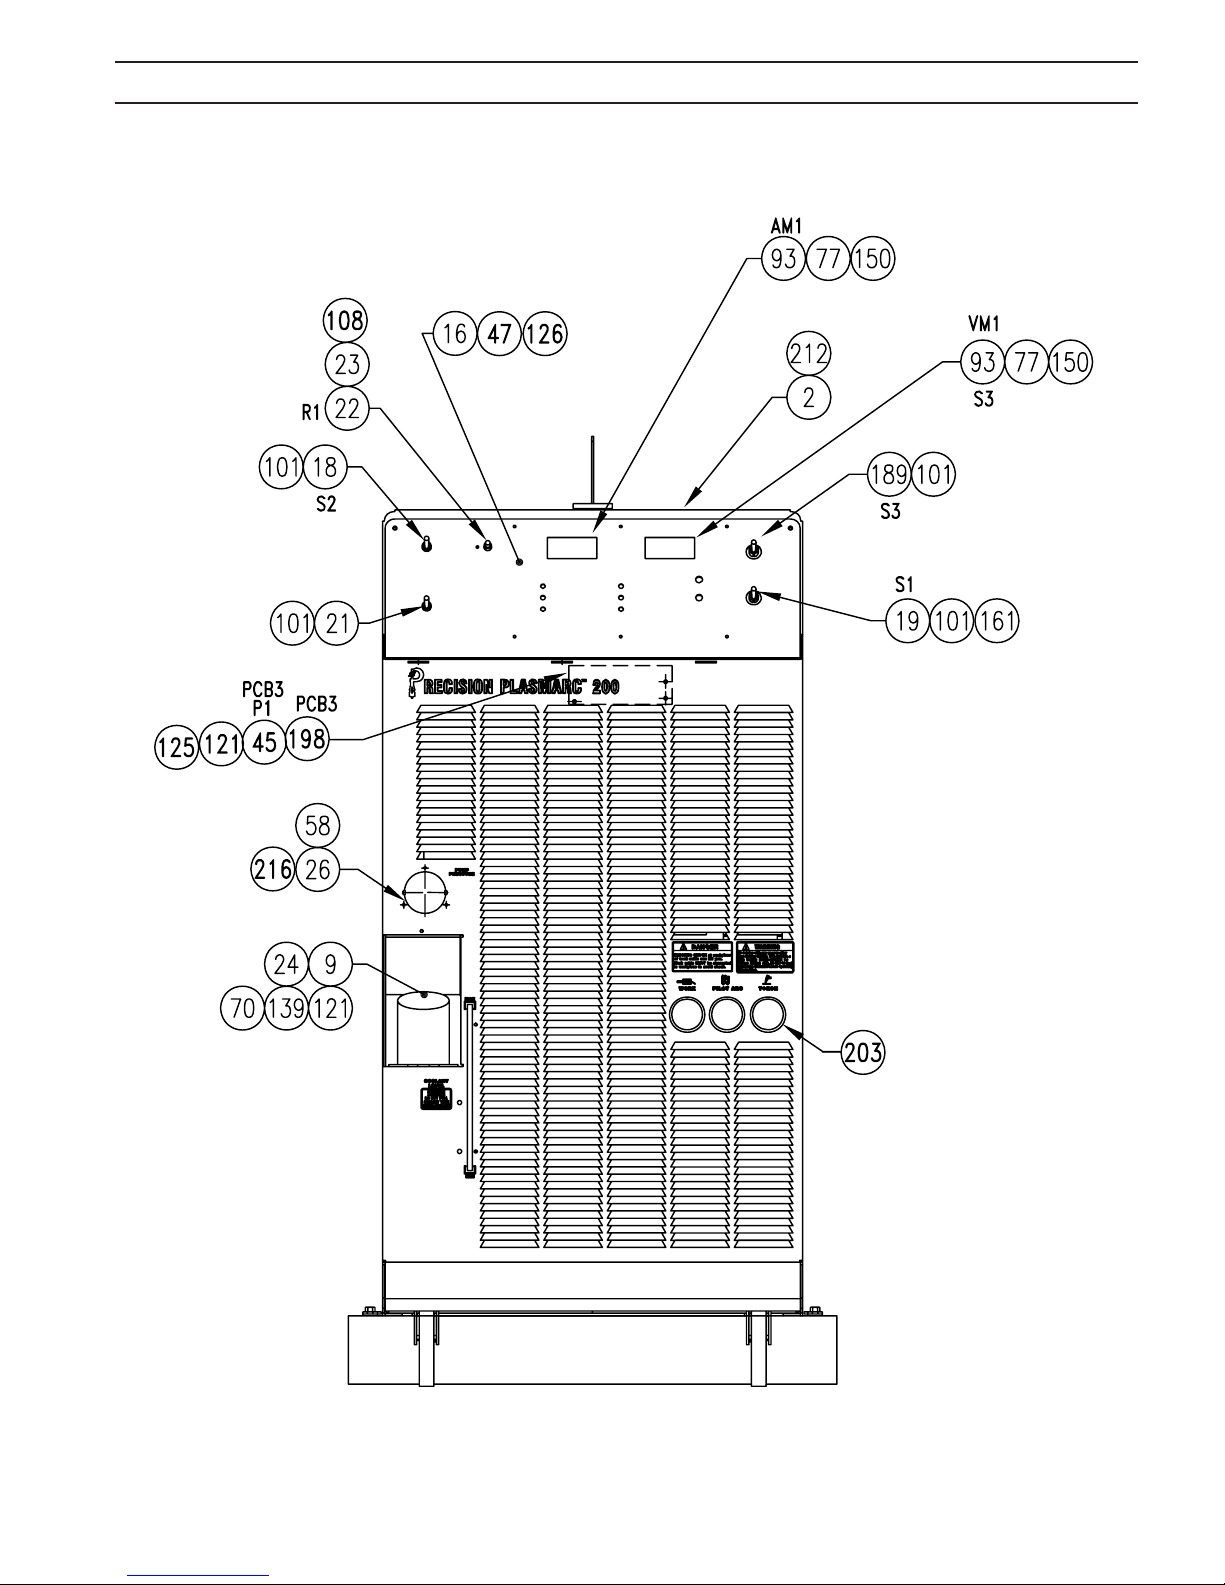
SECTION 7 REPLACEMENT PARTS
40
Page 41
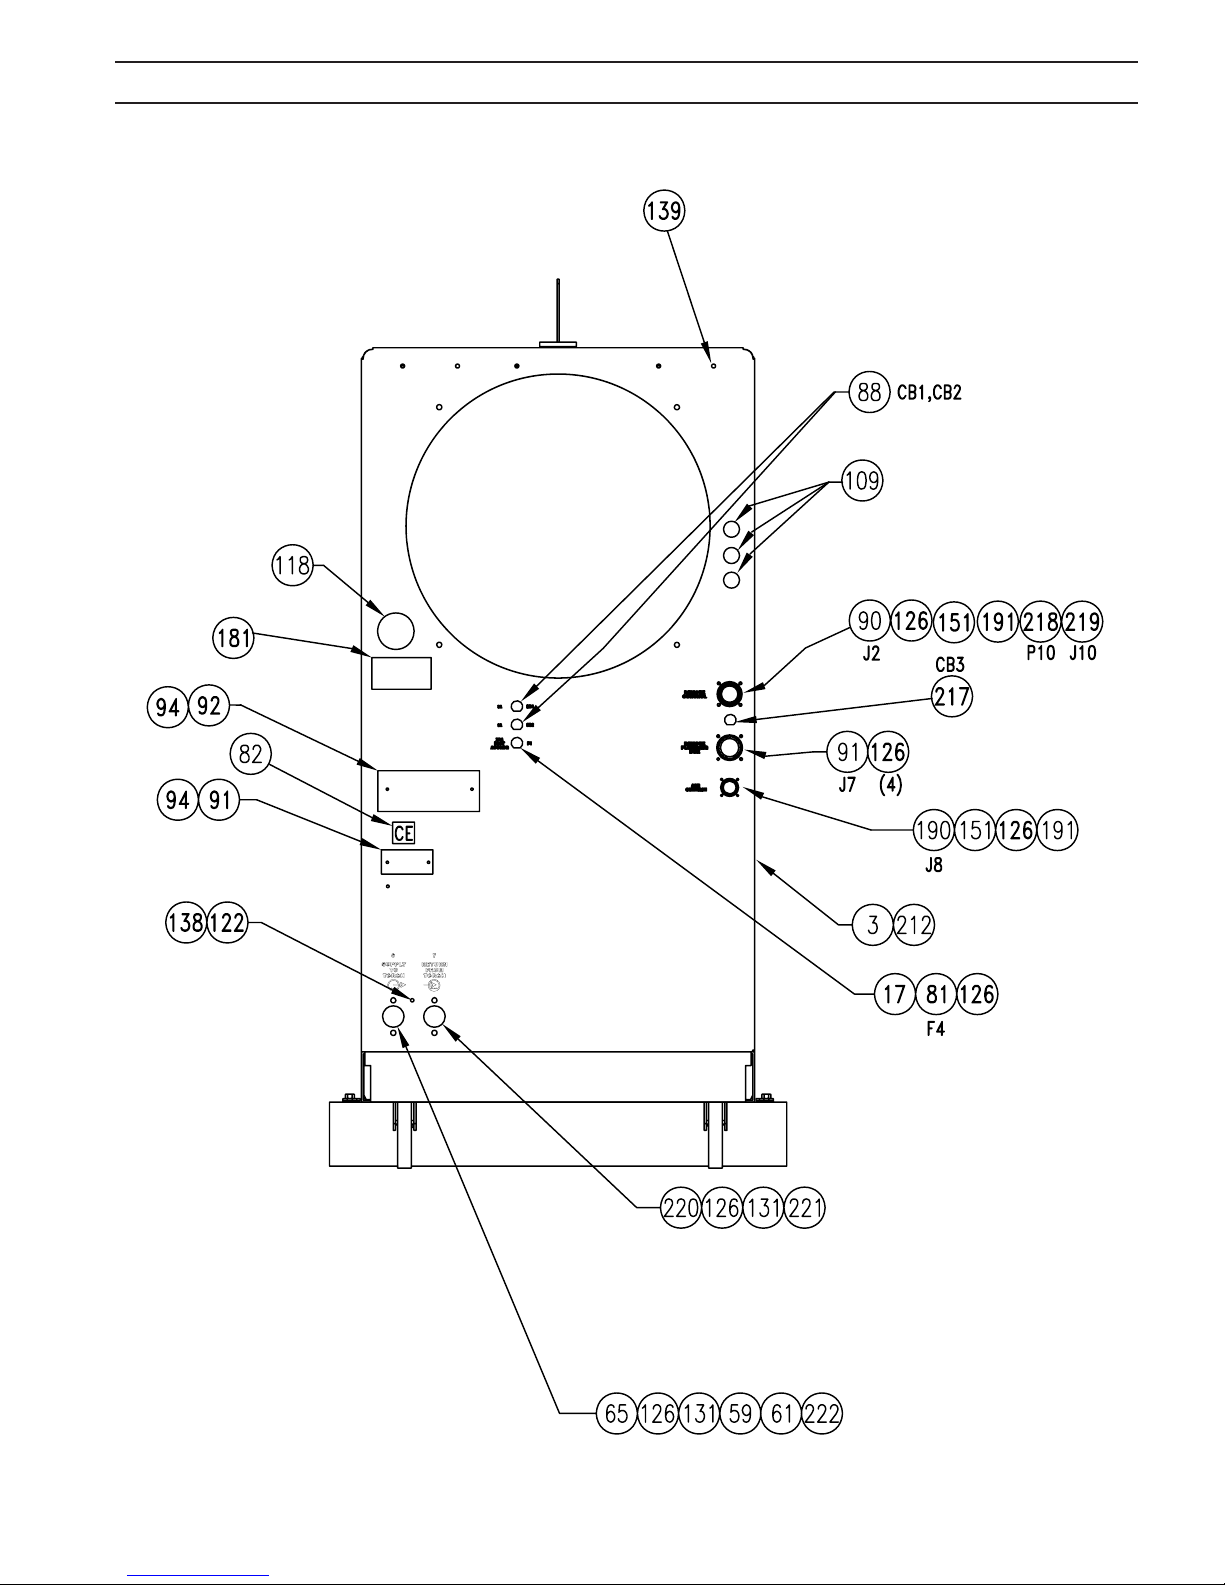
SECTION 7 REPLACEMENT PARTS
41
Page 42
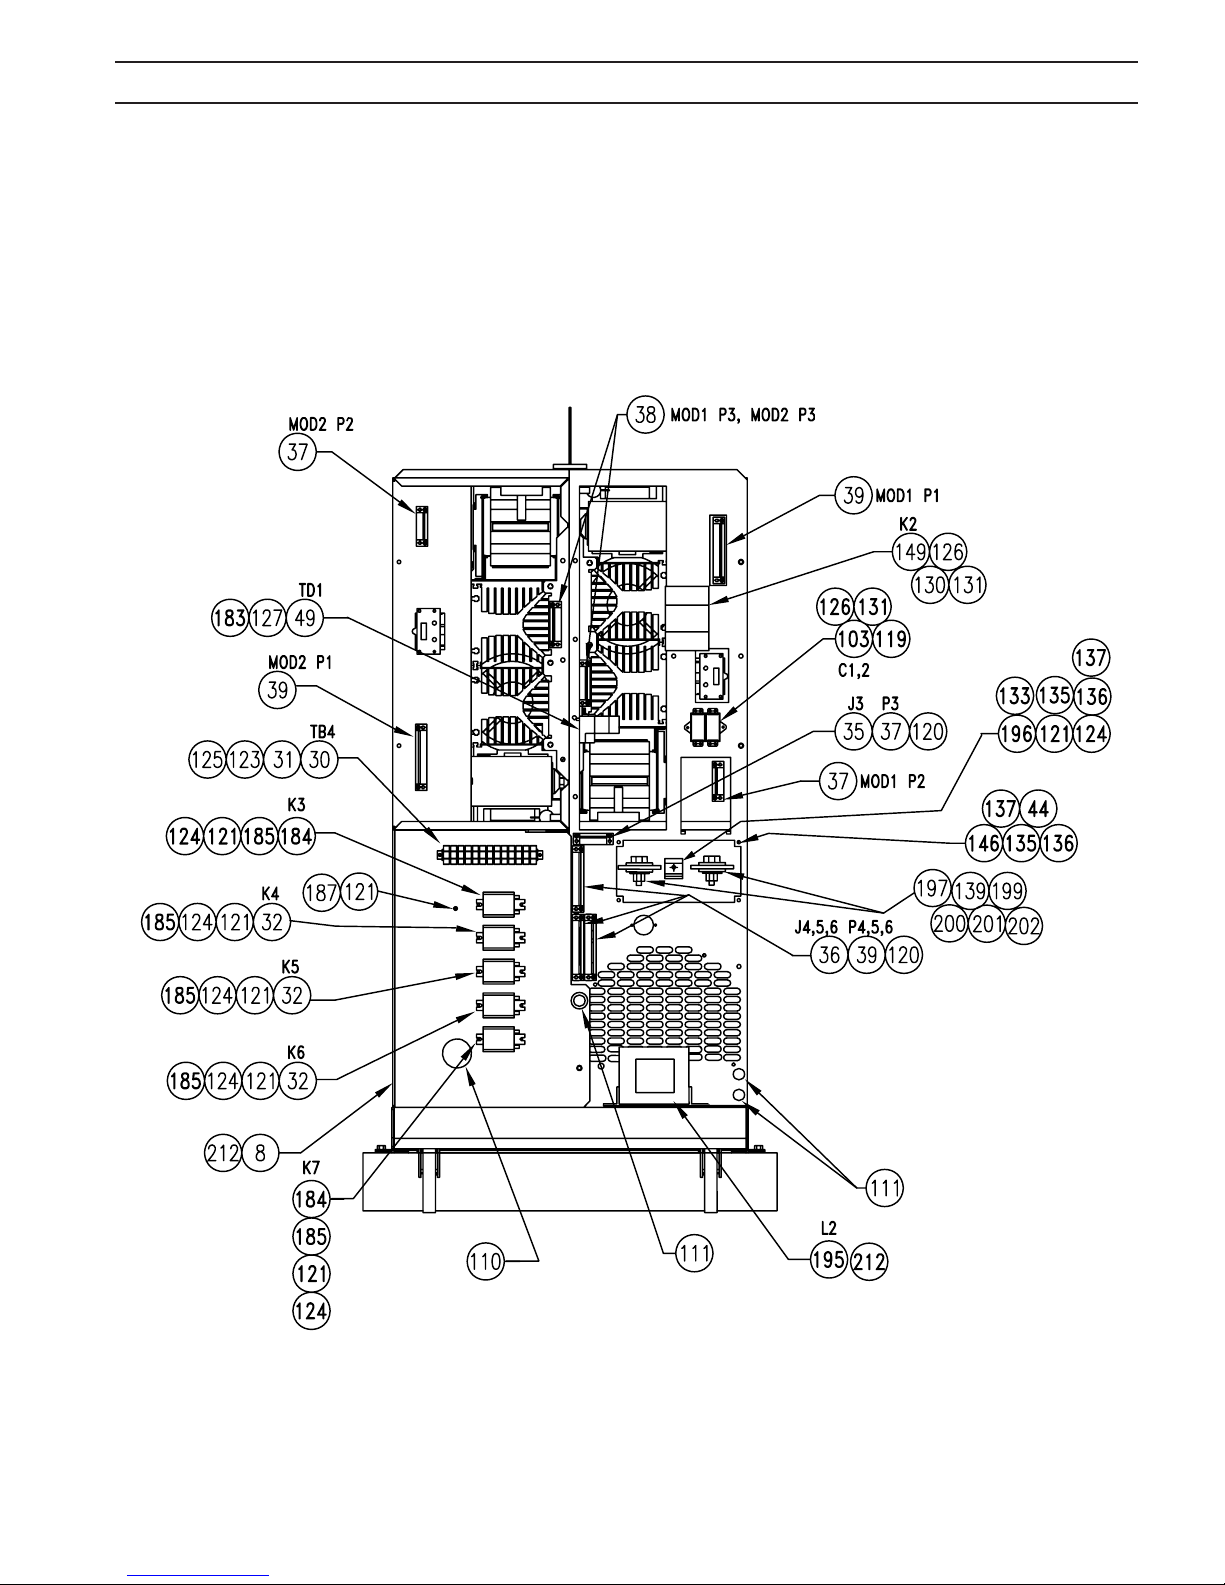
SECTION 7 REPLACEMENT PARTS
42
Page 43
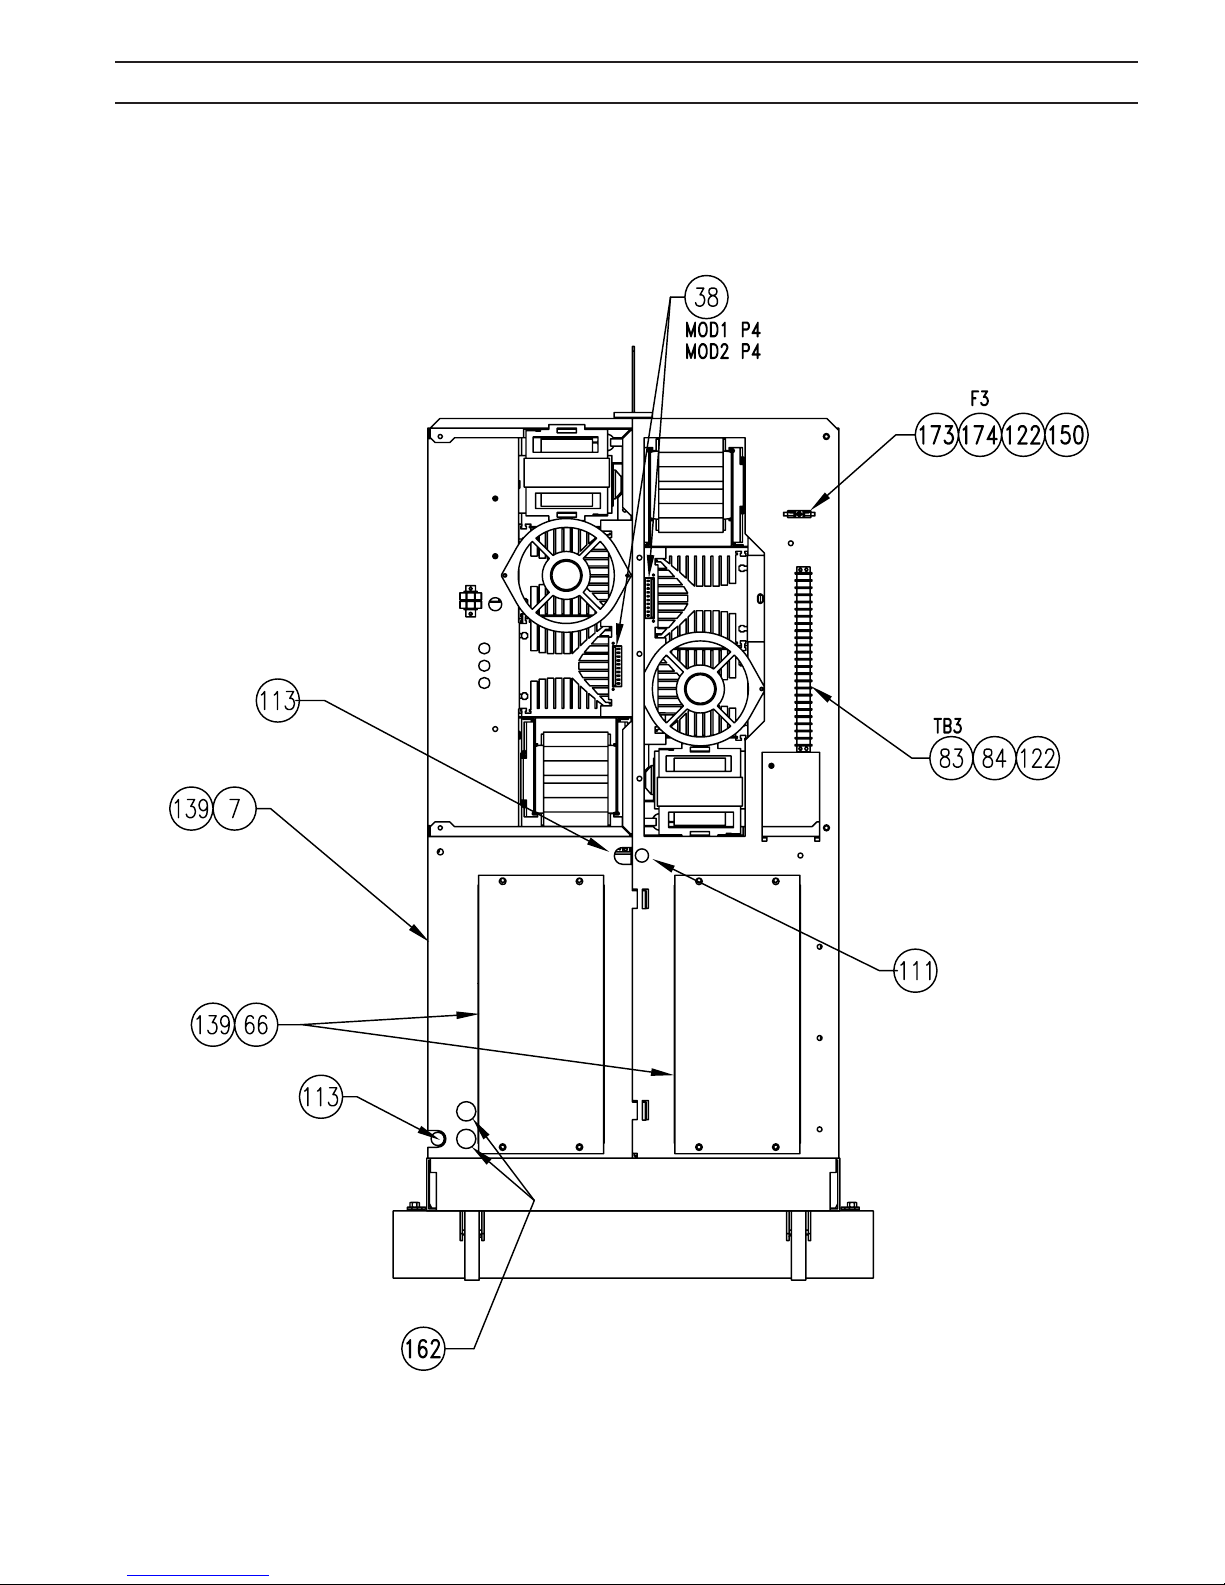
SECTION 7 REPLACEMENT PARTS
43
Page 44
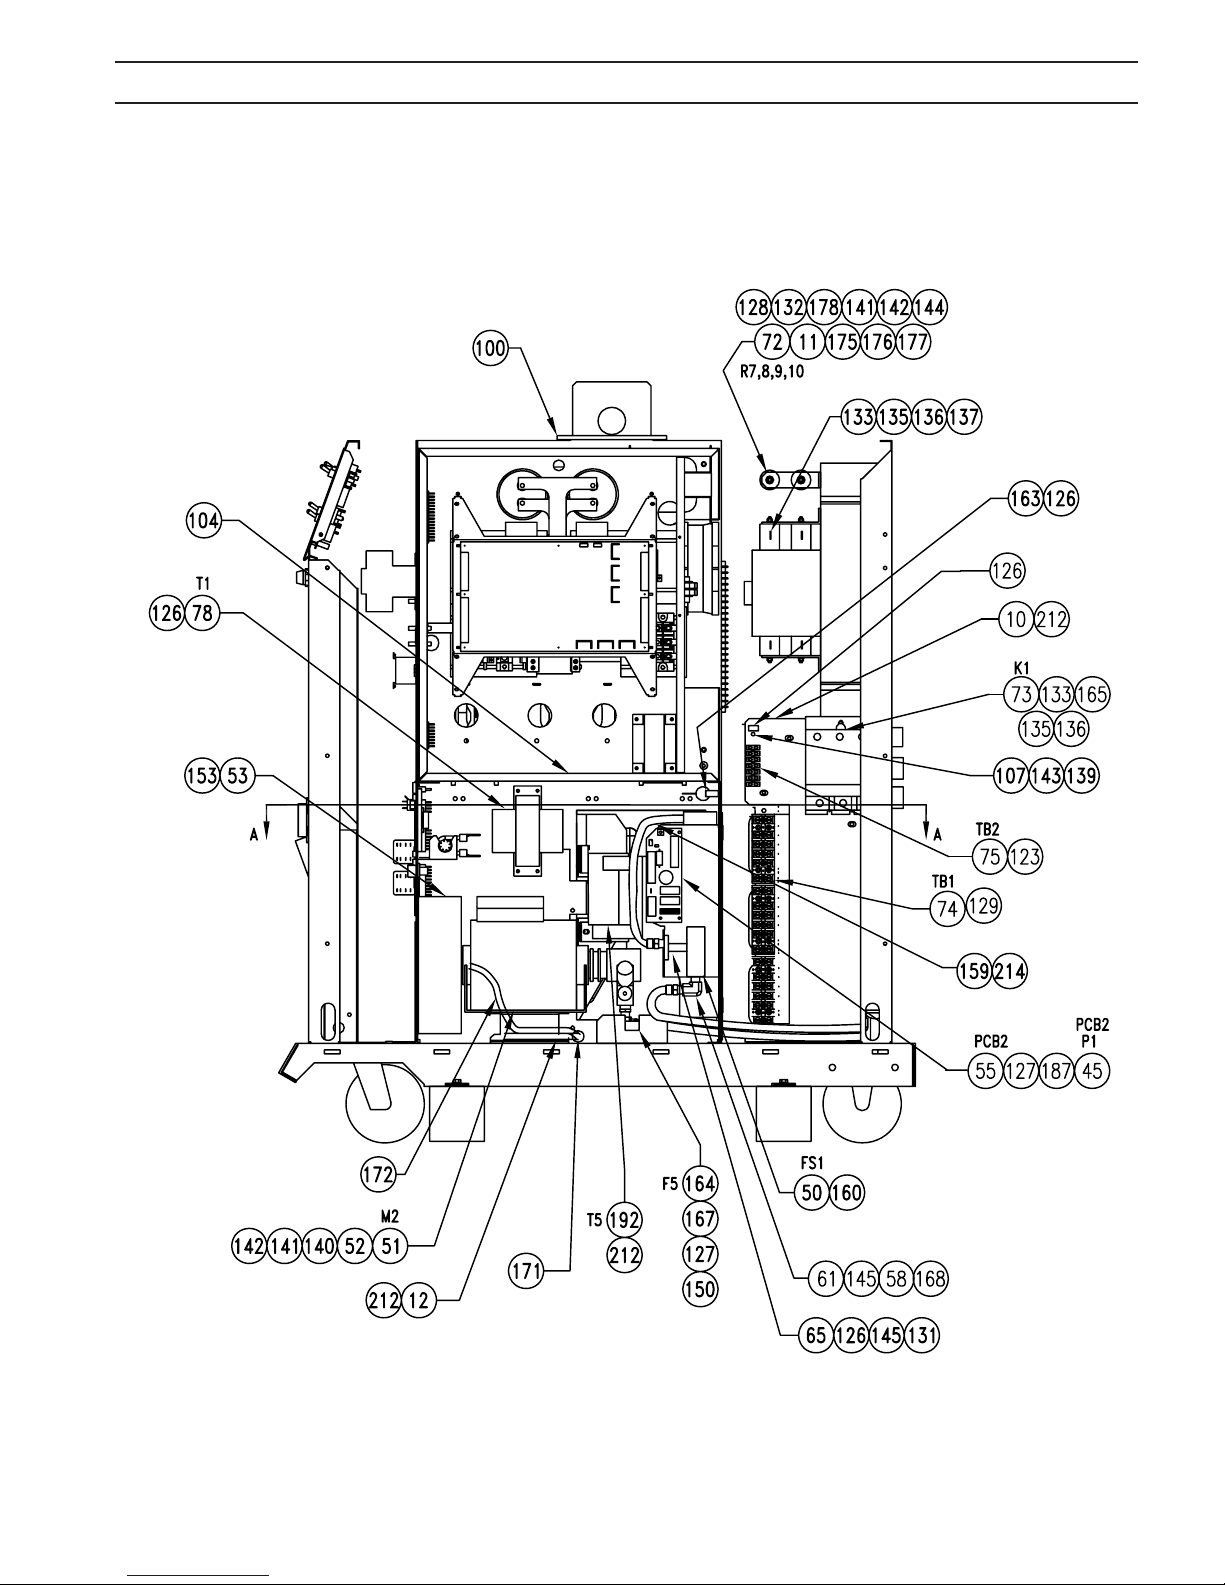
SECTION 7 REPLACEMENT PARTS
44
Page 45
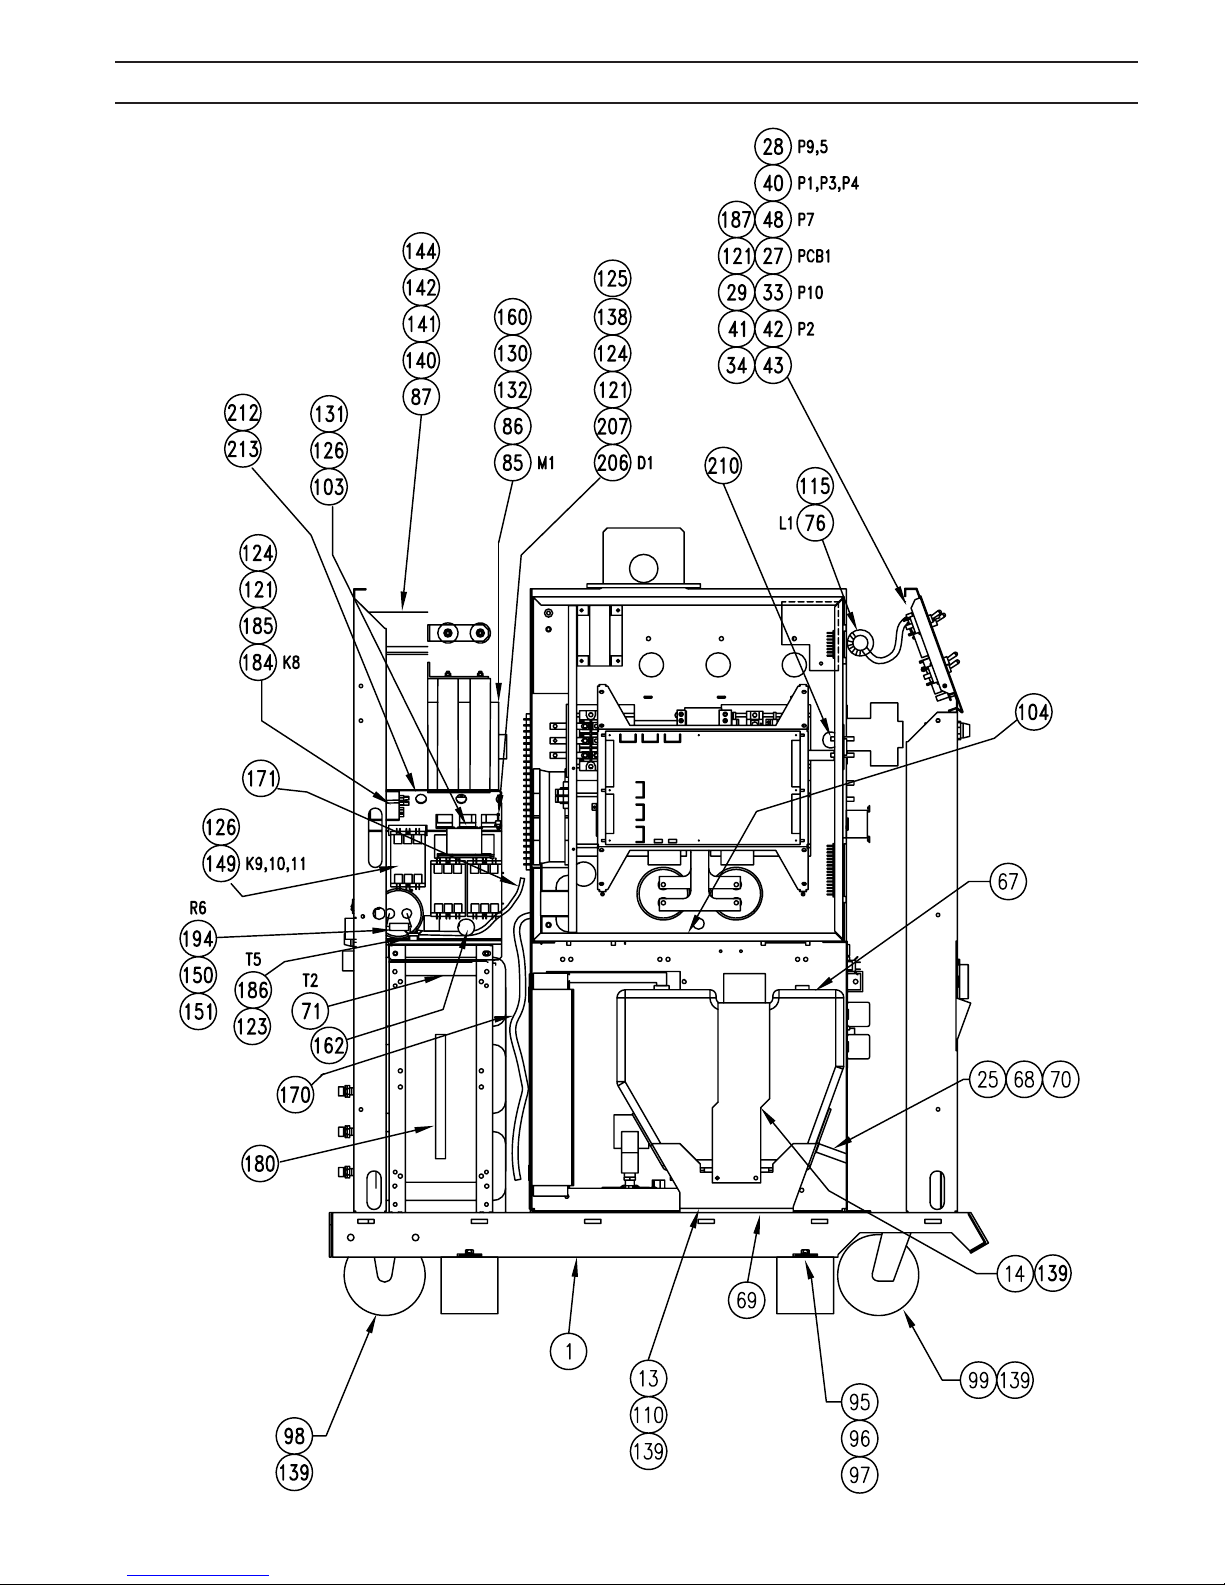
SECTION 7 REPLACEMENT PARTS
45
Page 46
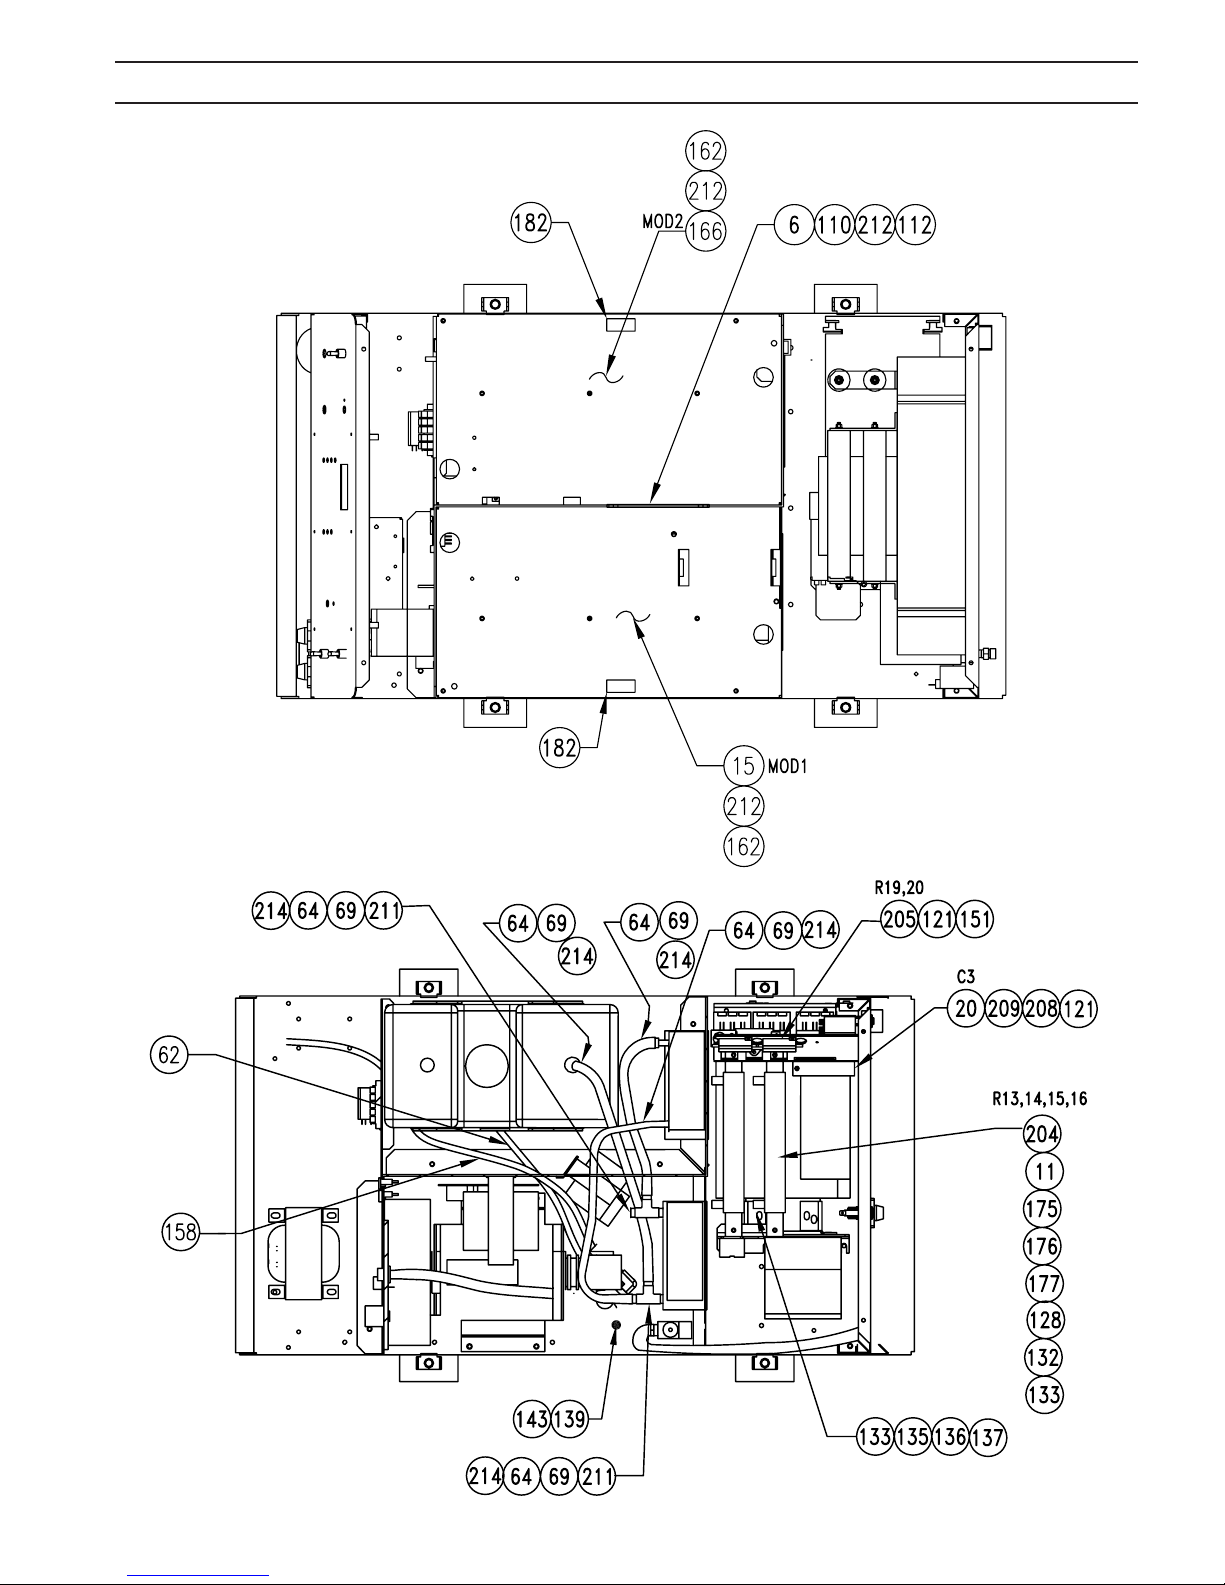
SECTION 7 REPLACEMENT PARTS
46
Page 47
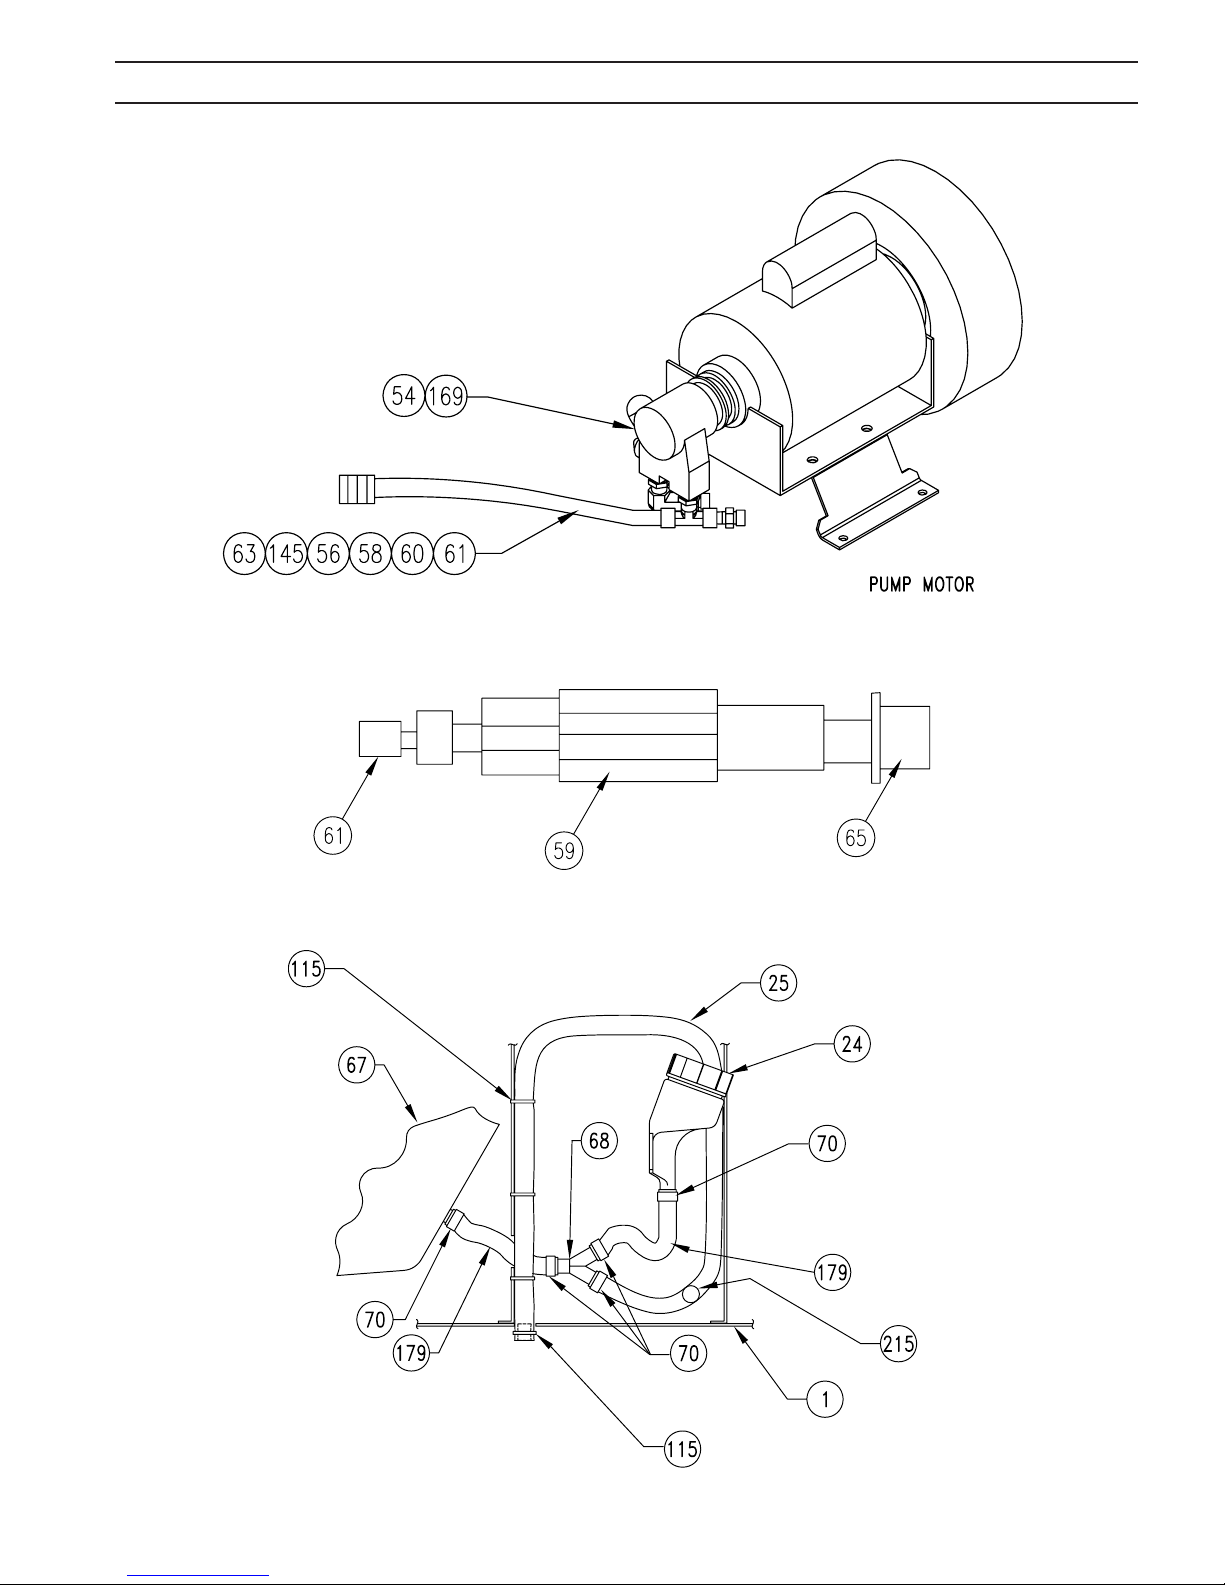
SECTION 7 REPLACEMENT PARTS
47
Page 48
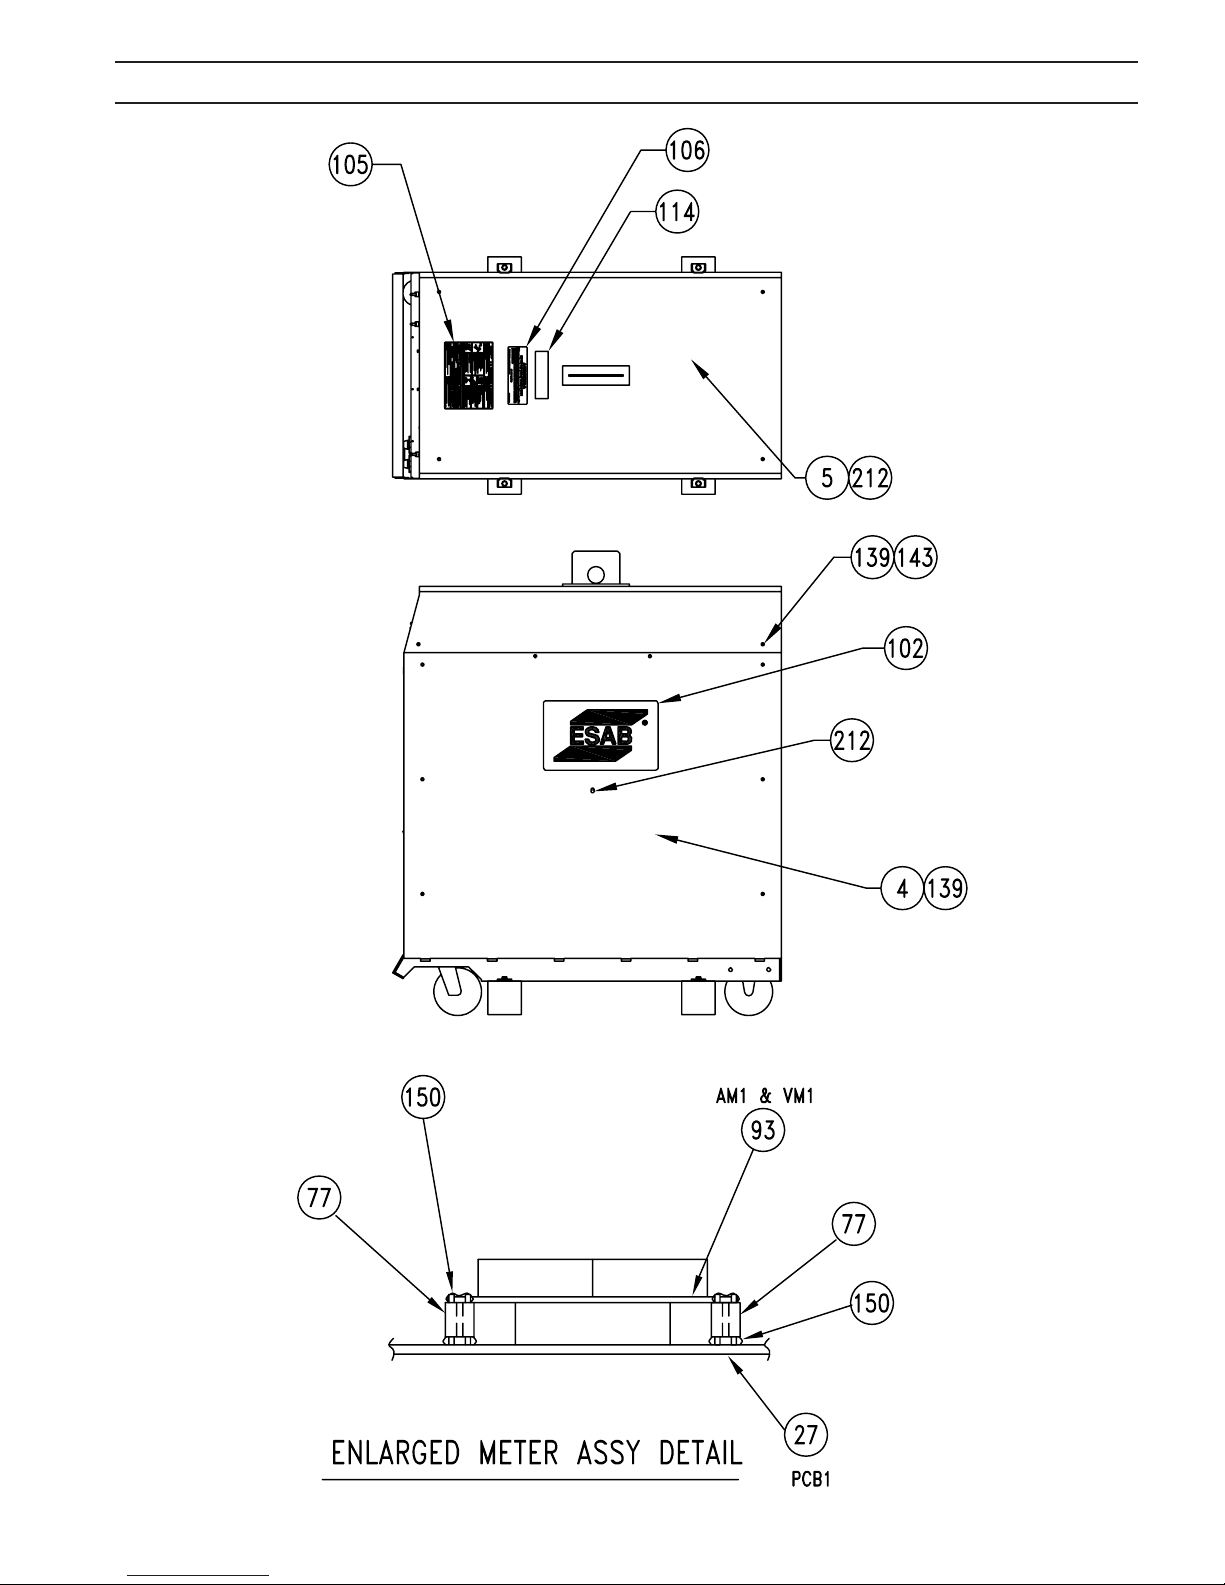
SECTION 7 REPLACEMENT PARTS
48
Page 49
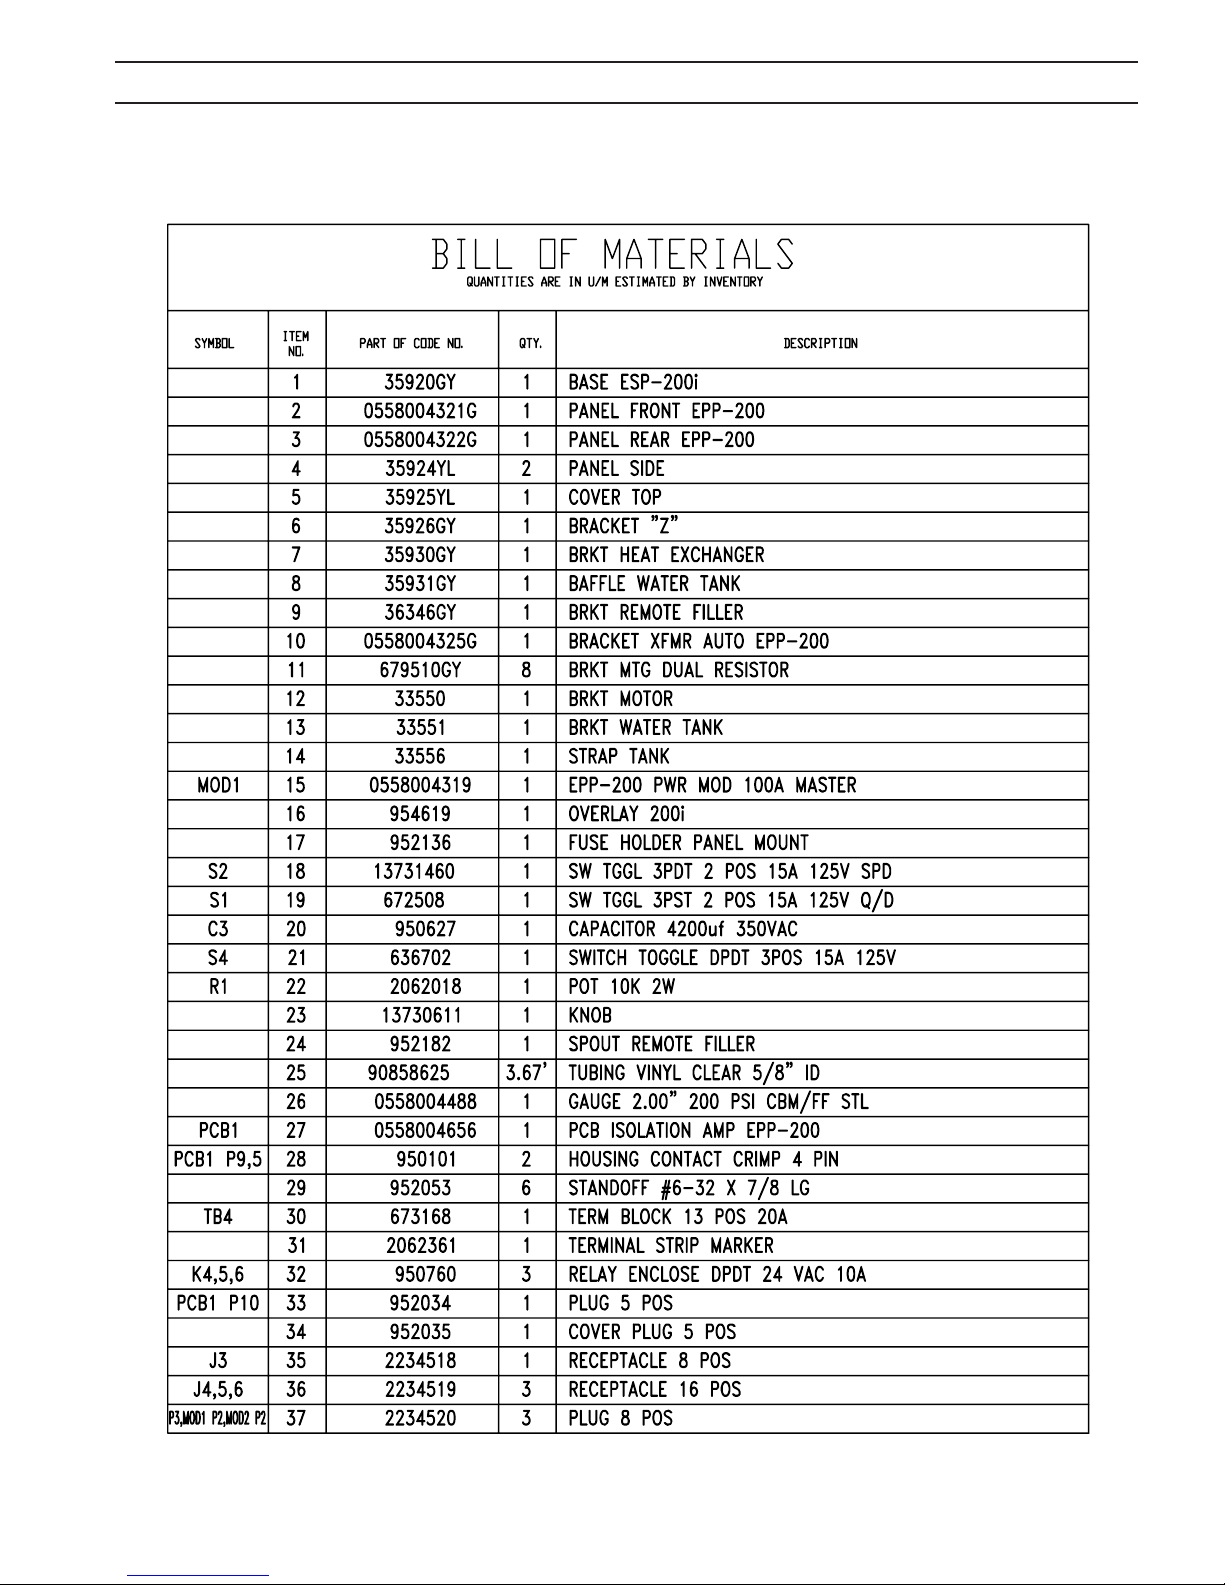
SECTION 7 REPLACEMENT PARTS
49
Page 50
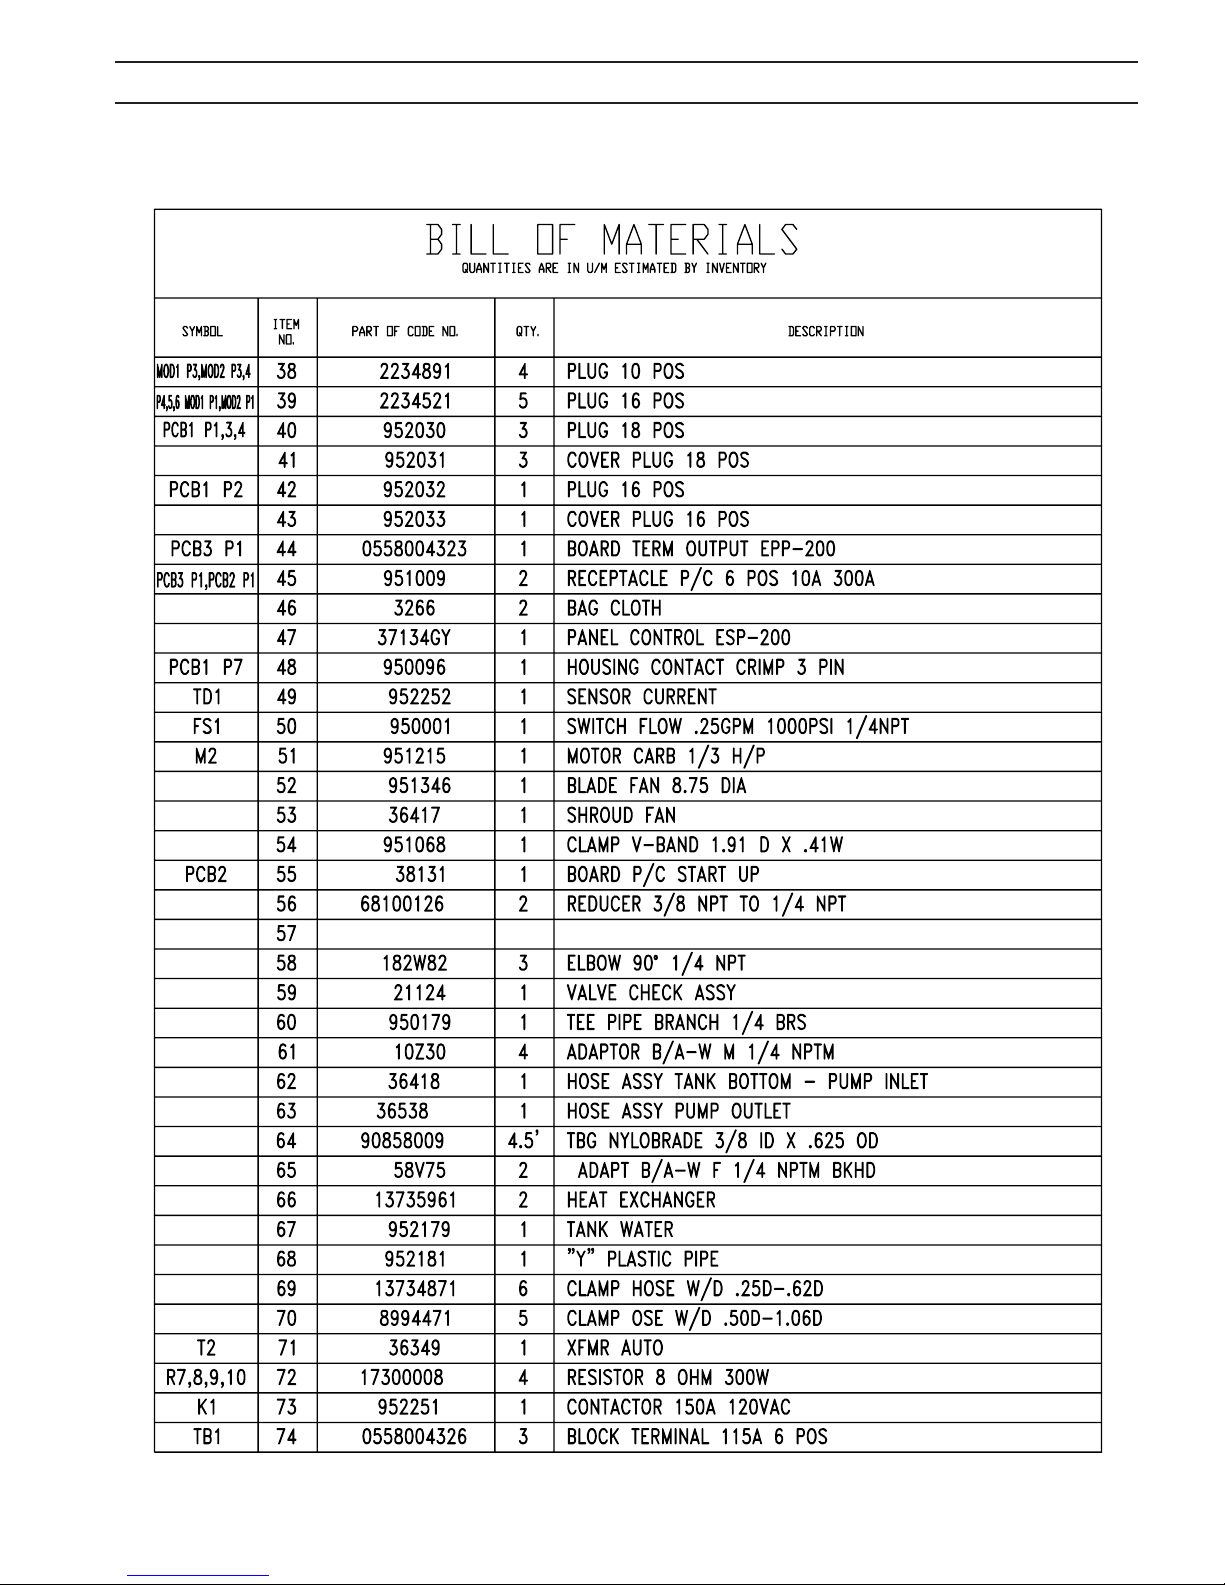
SECTION 7 REPLACEMENT PARTS
50
Page 51
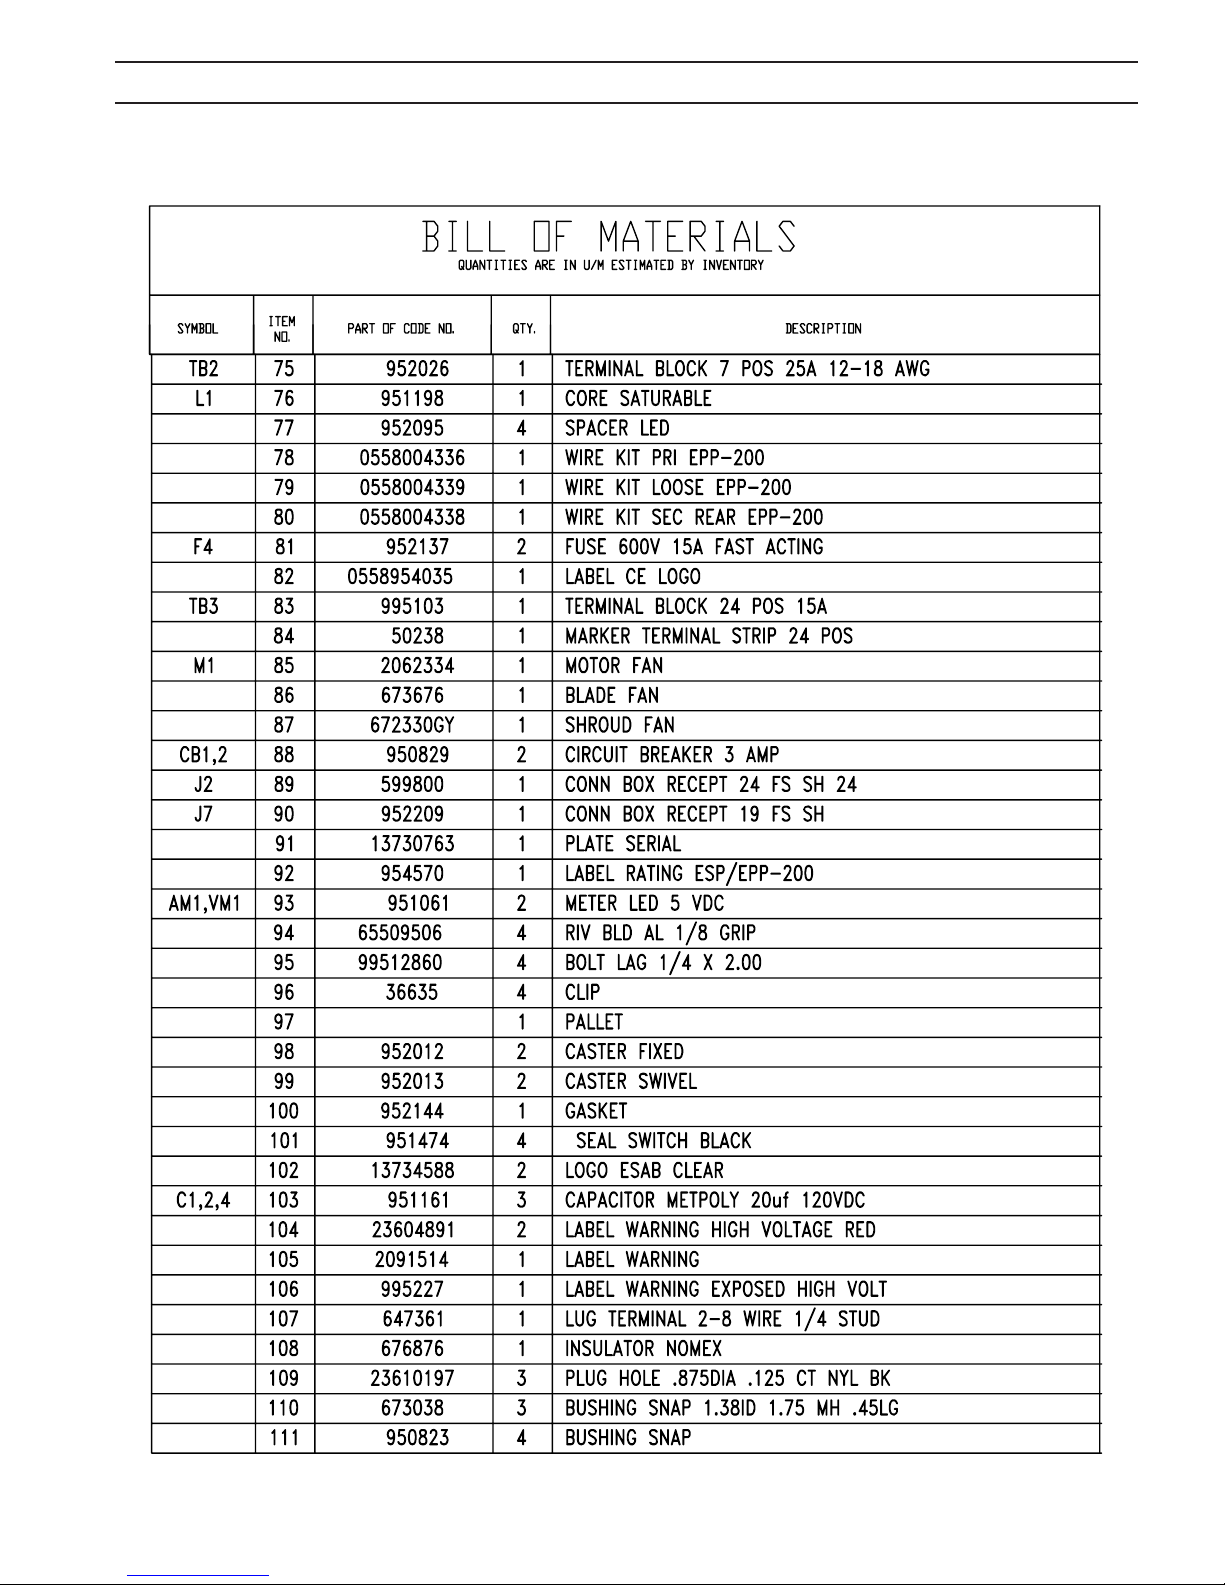
SECTION 7 REPLACEMENT PARTS
51
Page 52
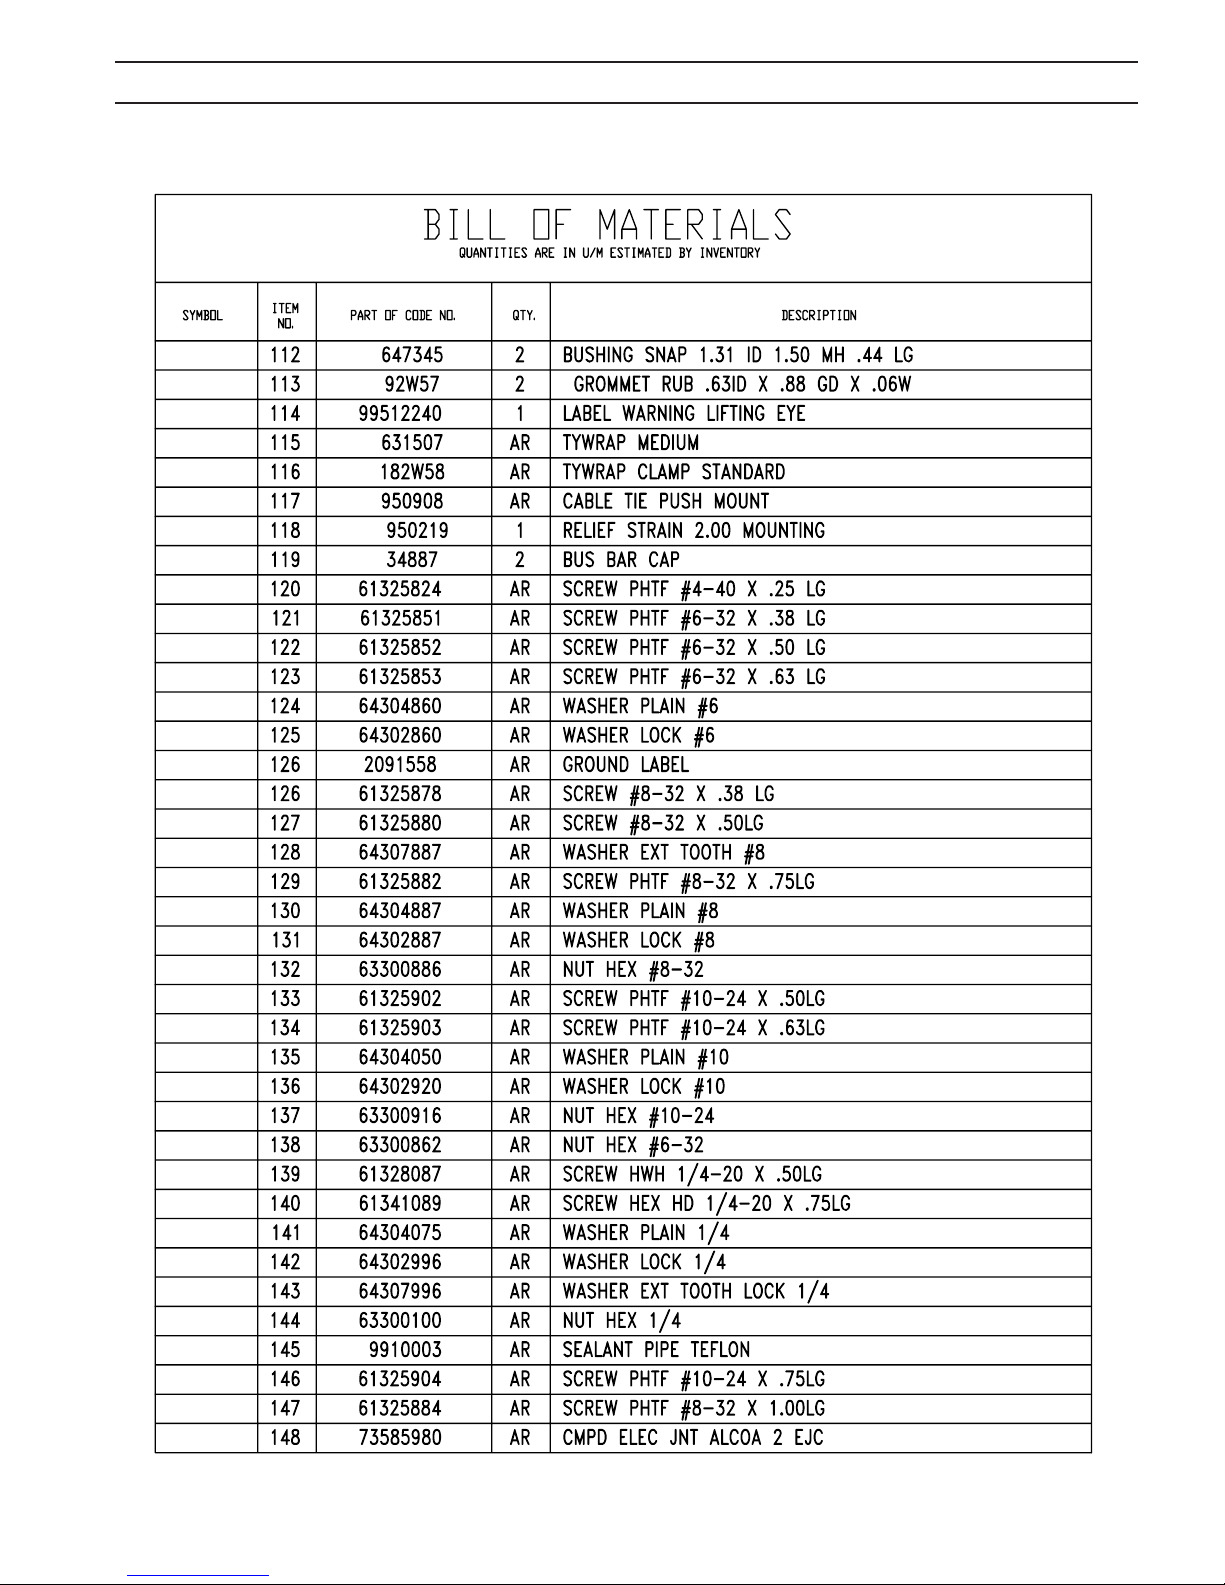
SECTION 7 REPLACEMENT PARTS
52
Page 53
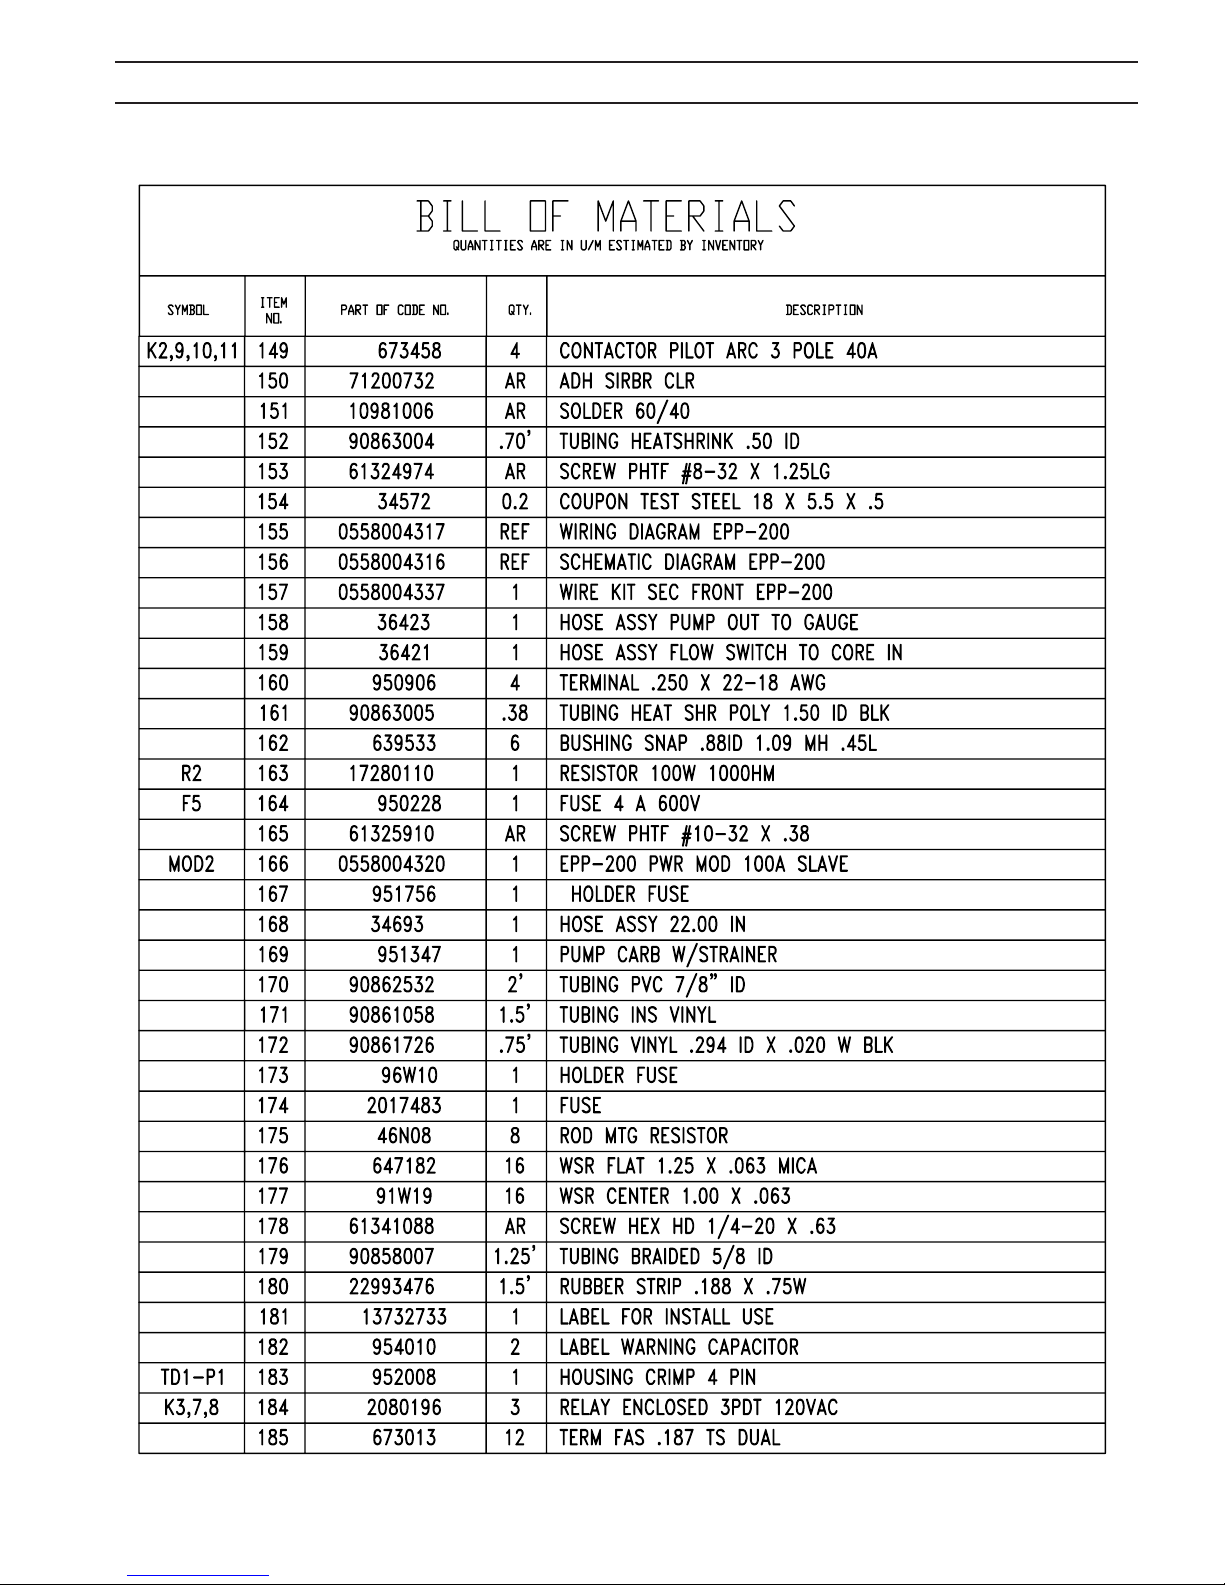
SECTION 7 REPLACEMENT PARTS
53
Page 54
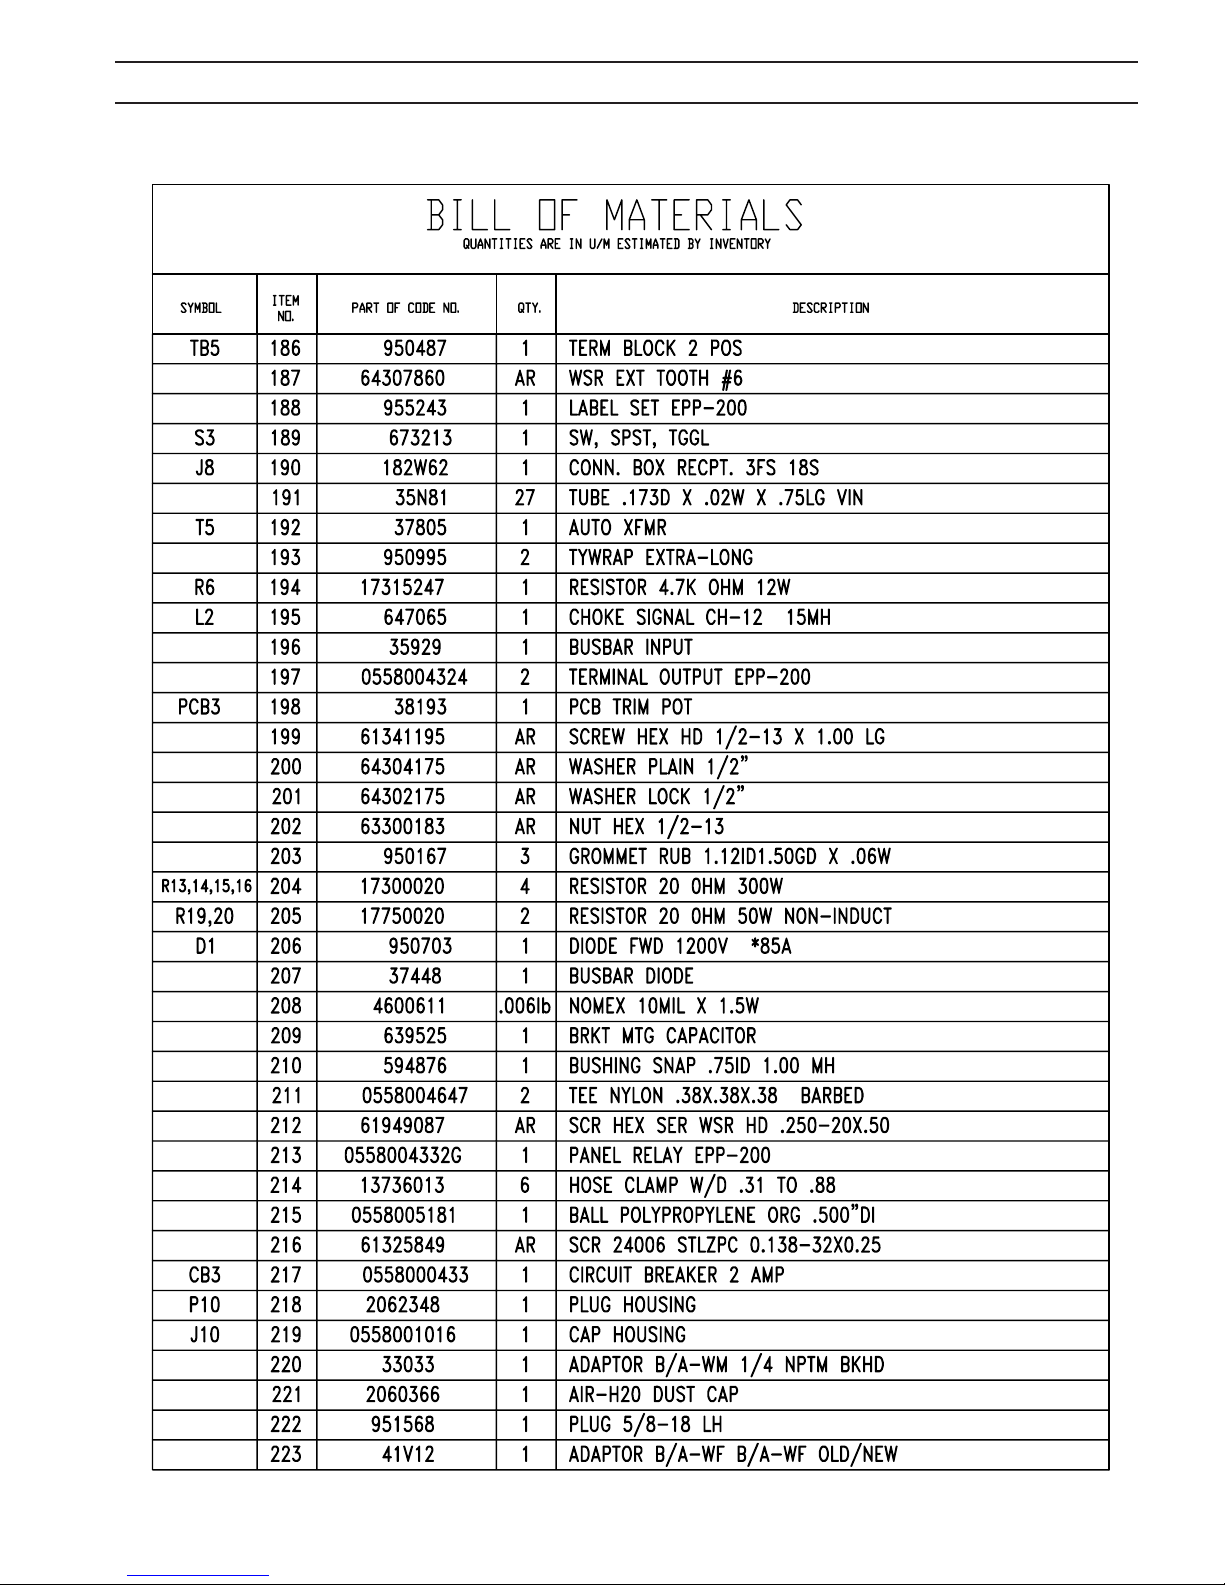
SECTION 7 REPLACEMENT PARTS
Page 55
Revision History
OriginalreleaseFebruary,2004
May,2004-ConvertedSchematicsandWiringDiagramsto11'x17'pagesizeandincludedatbackof
manual.
June,2004-UpdatedOptions,AccessoriesandHosechartsonPages13and14.
November,2004-Changedbomitem69from:clamphosew/d.25d-.62dqty:12to:clamphosew/d
.31d - .88d qty: 6.
February,2006-UpdatedSchematicandReplacementPartsperECN#053186.
November,2006-UpdatedReplacementParts
December,2006-UpdatedReplacementParts
October,2007-Updatedconductor/fusetableinSubsection3.4.1.Updateddisclaimerpage.
Page 56
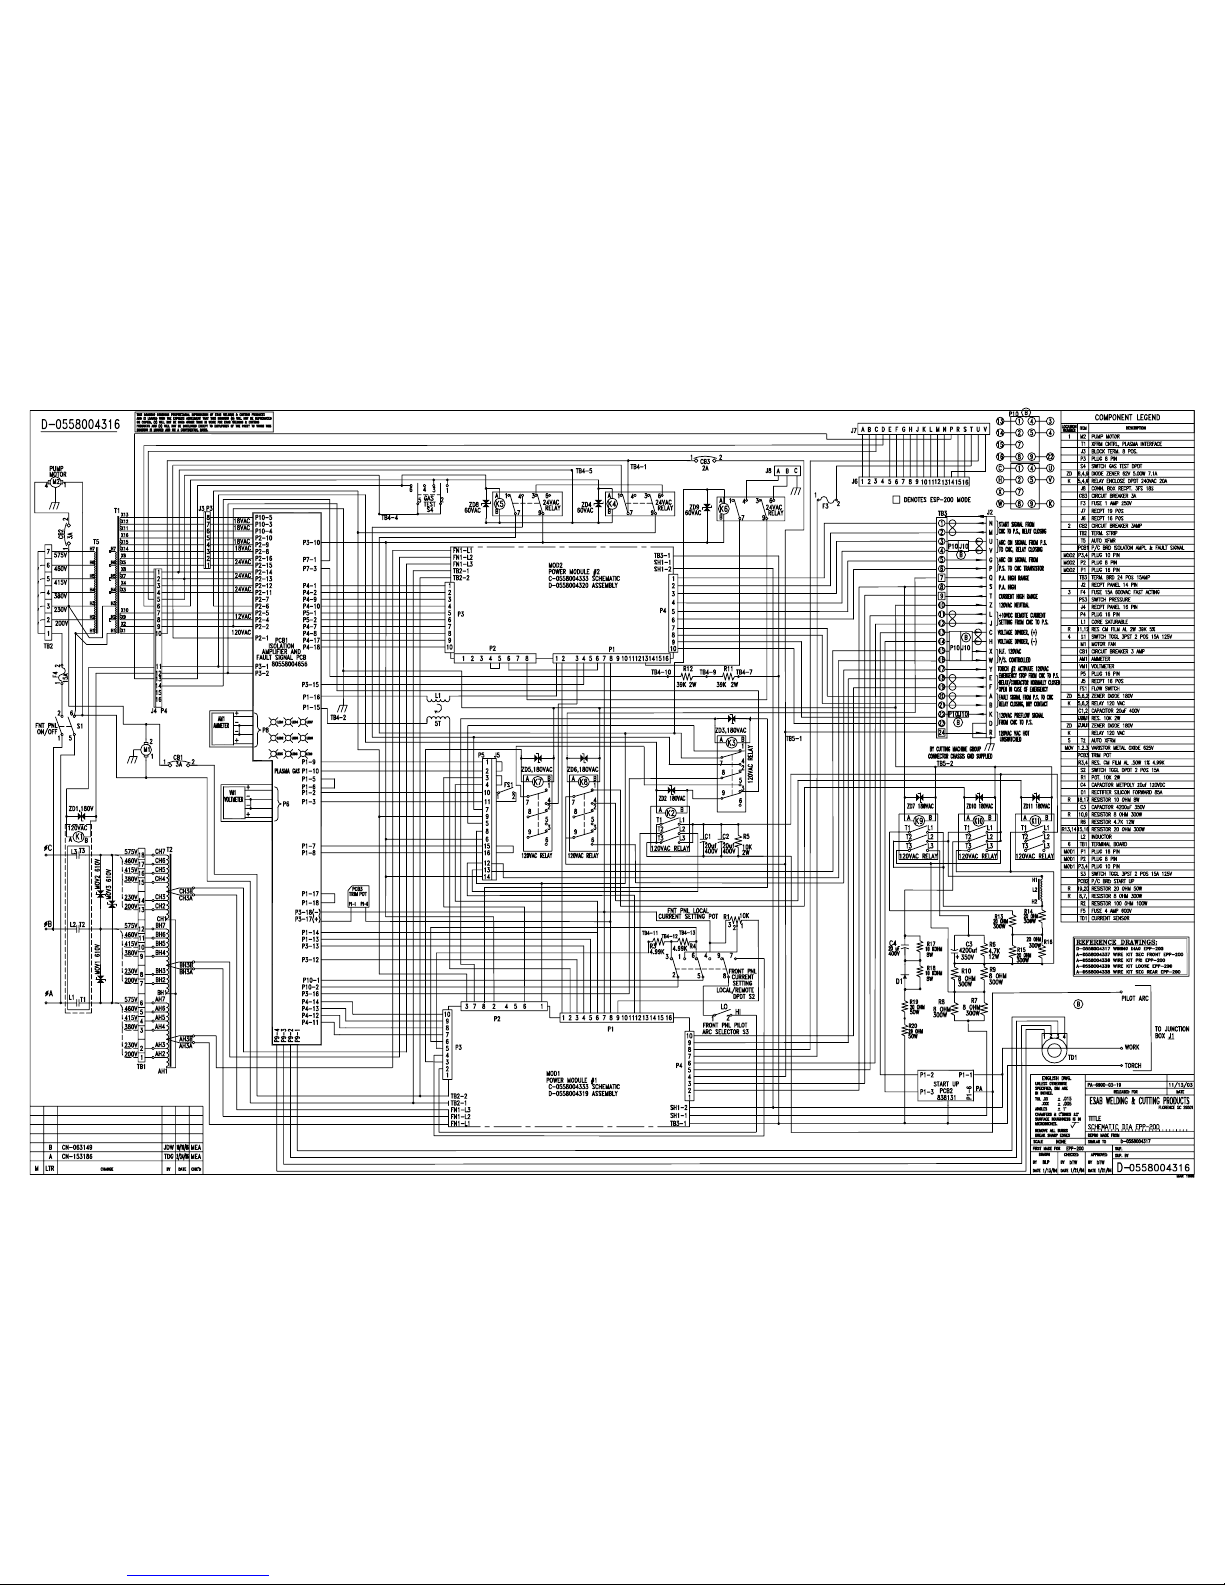
Page 57
Page 58
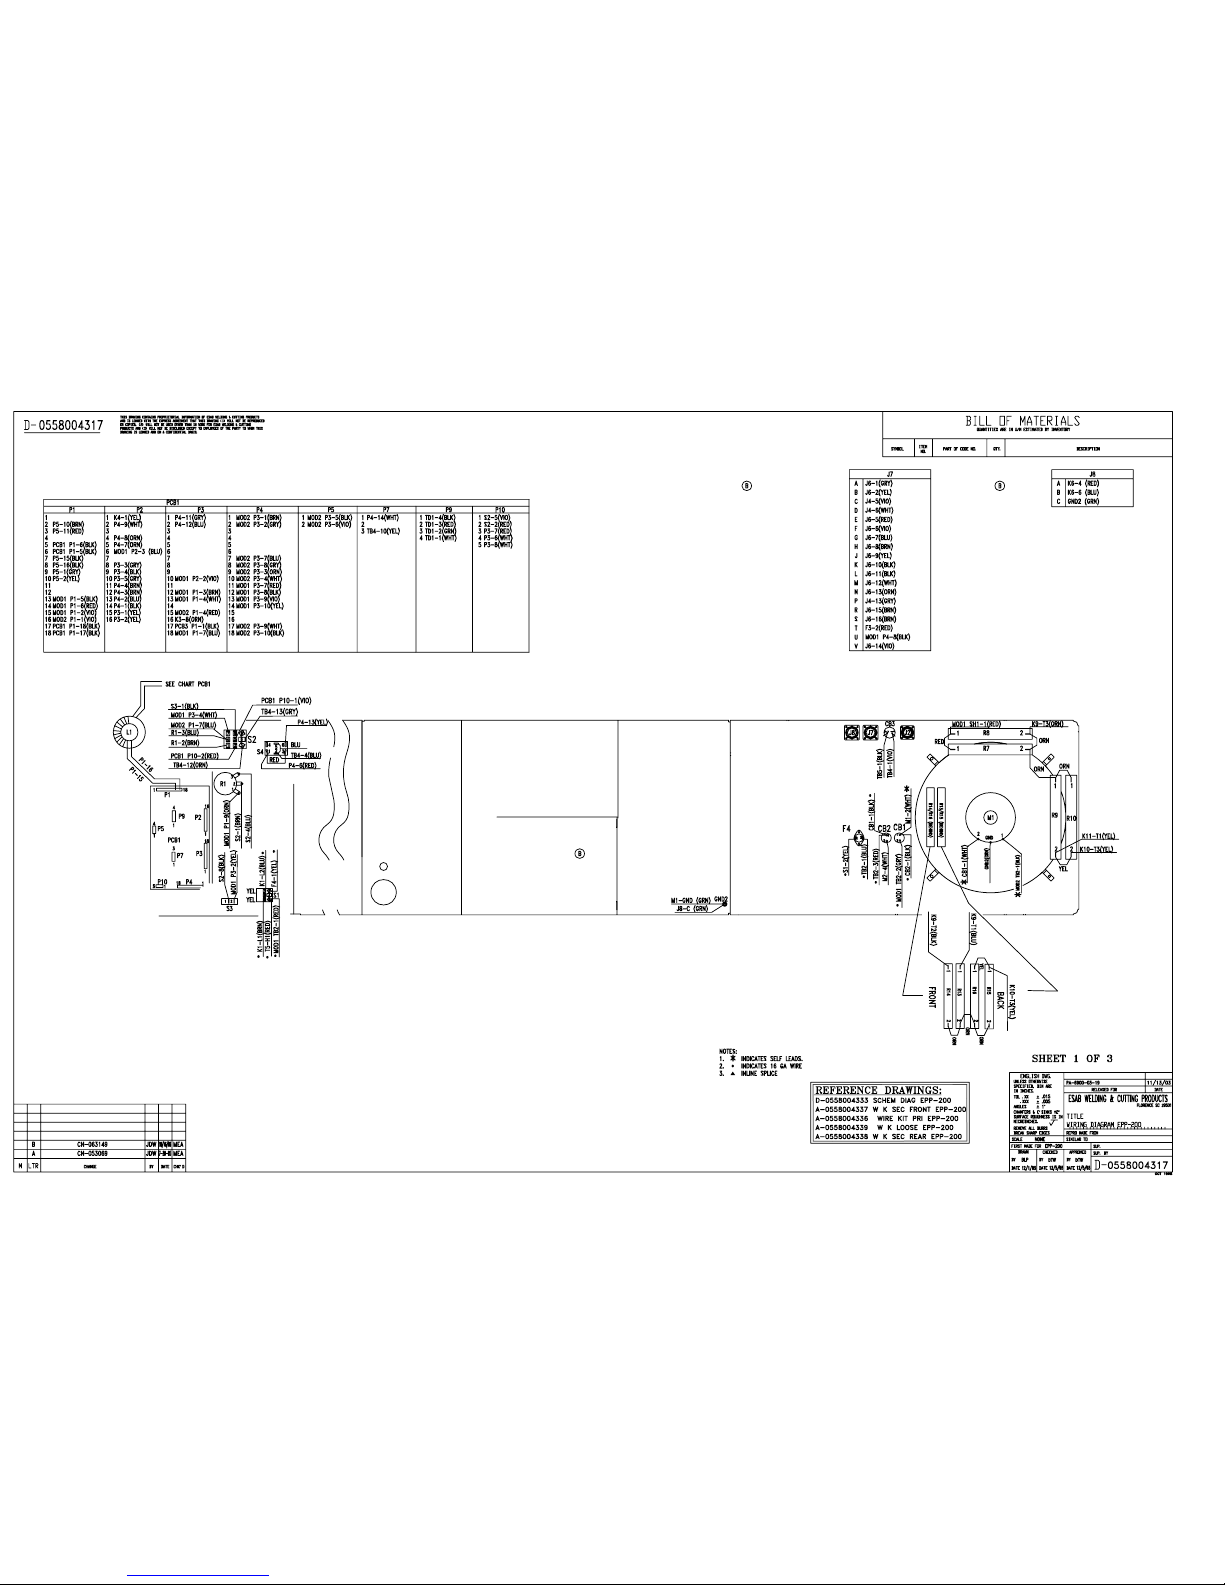
Page 59
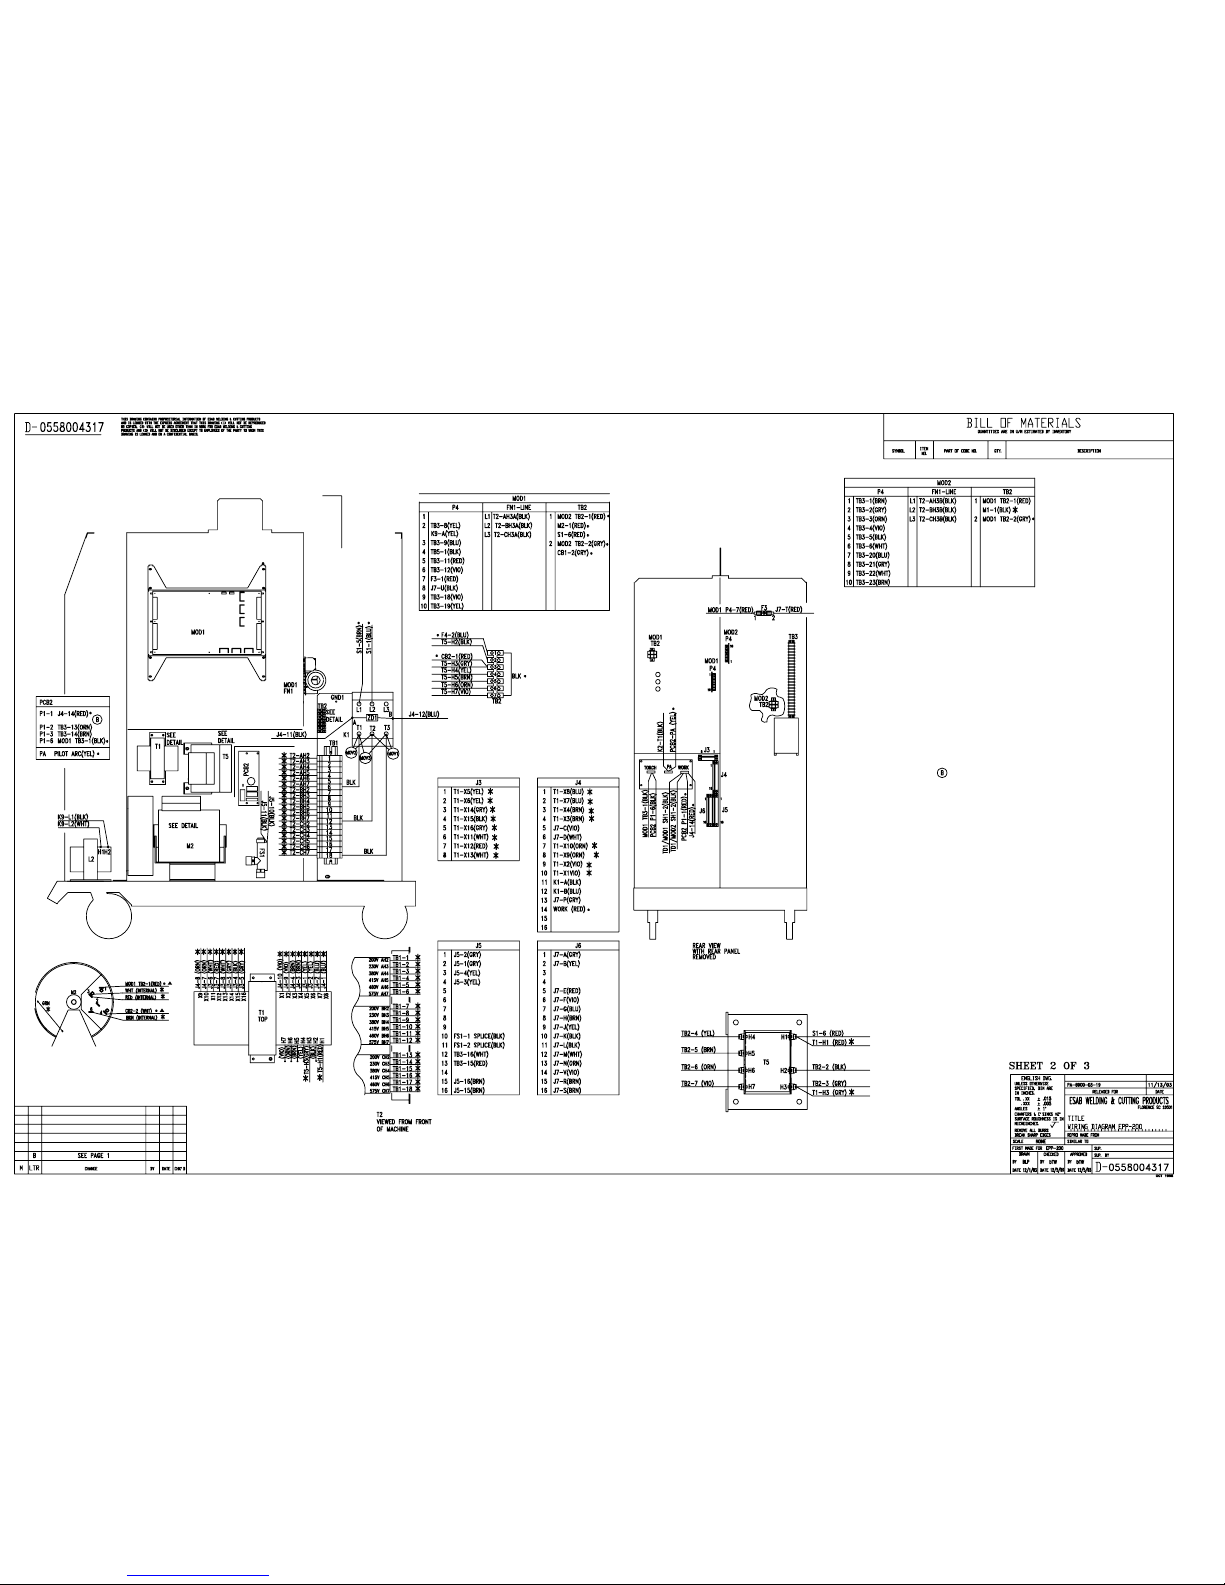
Page 60
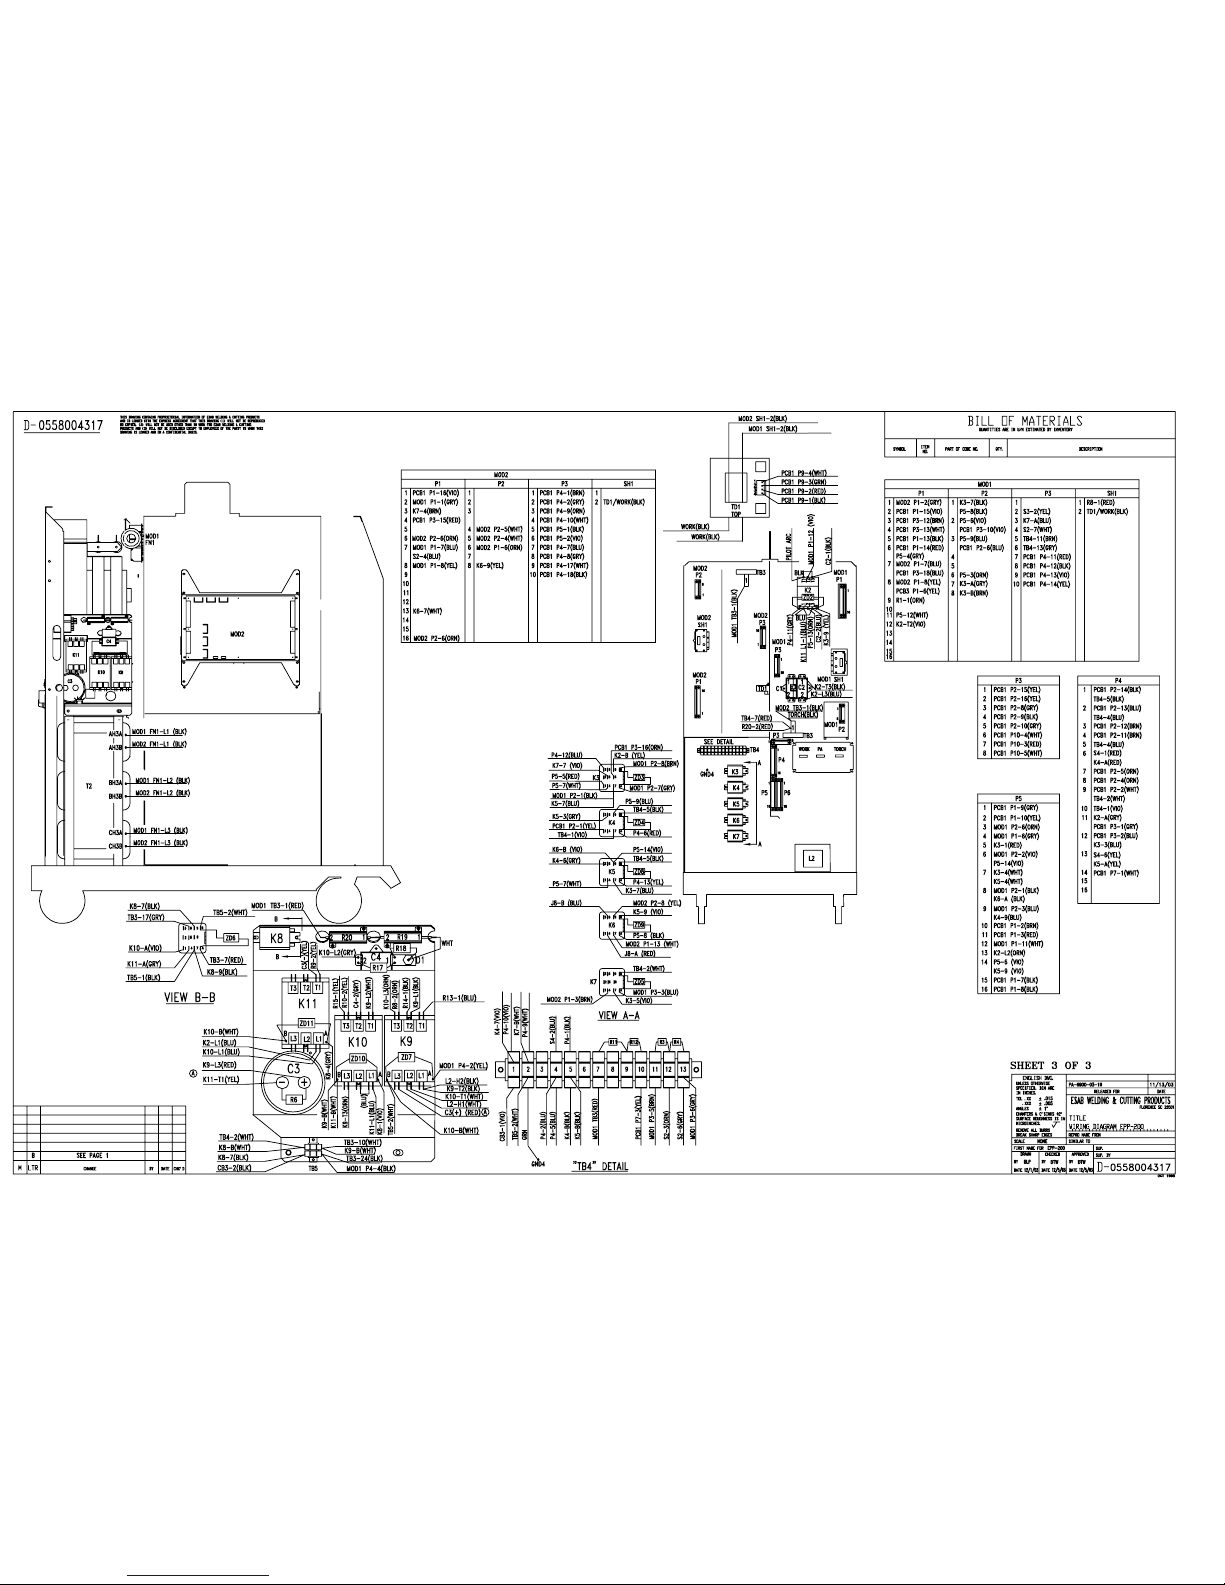
Page 61
Page 62
ESAB Welding & Cutting Products, Florence, SC Welding Equipment
COMMUNICATION GUIDE - CUSTOMER SERVICES
A. CUSTOMER SERVICE QUESTIONS:
Telephone: (800)362-7080 / Fax: (800) 634-7548 Hours: 8:00 AM to 7:00 PM EST
Order Entry Product Availability Pricing Order Information Returns
B. ENGINEERING SERVICE:
Telephone: (843) 664-4416 / Fax : (800) 446-5693 Hours: 7:30 AM to 5:00 PM EST
Warranty Returns Authorized Repair Stations Welding Equipment Troubleshooting
C. TECHNICAL SERVICE:
Telephone: (800) ESAB-123/ Fax: (843) 664-4452 Hours: 8:00 AM to 5:00 PM EST
Part Numbers Technical Applications Specications Equipment Recommendations
D. LITERATURE REQUESTS:
Telephone: (843) 664-5562 / Fax: (843) 664-5548 Hours: 7:30 AM to 4:00 PM EST
E. WELDING EQUIPMENT REPAIRS:
Telephone: (843) 664-4487 / Fax: (843) 664-5557 Hours: 7:30 AM to 3:30 PM EST
Repair Estimates Repair Status
F. WELDING EQUIPMENT TRAINING
Telephone: (843)664-4428 / Fax: (843) 679-5864 Hours: 7:30 AM to 4:00 PM EST
Training School Information and Registrations
G. WELDING PROCESS ASSISTANCE:
Telephone: (800) ESAB-123 Hours: 7:30 AM to 4:00 PM EST
H. TECHNICAL ASST. CONSUMABLES:
Telephone : (800) 933-7070 Hours: 7:30 AM to 5:00 PM EST
IF YOU DO NOT KNOW WHOM TO CALL
Telephone: (800) ESAB-123
Fax: (843) 664-4462
Hours: 7:30 AM to 5:00 PM EST
or
visit us on the web at http://www.esabna.com
The ESAB web site oers
Comprehensive Product Information
Material Safety Data Sheets
Warranty Registration
Instruction Literature Download Library
Distributor Locator
Global Company Information
Press Releases
Customer Feedback & Support
0558004676 10 / 2007
 Loading...