

ESAB A6 S Arc Master, A6 S G Master, A6 S Compact 500, A6 SFE1, A6 SFE2 Instruction Manual
...Page 1

A6 S Arc Master
A6 S G Master
A6 S Compact 500
A6 SFE1 / A6 SFE2 / A6 SGE1/
A6 SFE1C
112101103105107109111102021110025108024042106023061104022041100020040060001
Bruksanvisning
Brugsanvisning
Bruksanvisning
Käyttöohjeet
Instruction manual
Betriebsanweisung
Manuel d’instructions
Gebruiksaanwijzing
Instrucciones de uso
Istruzioni per l’uso
Manual de instruções
ПдзгЯет чсЮуещт
Instrukcja obs³ugi
Valid for serial no. 3210456 562 101 2009--03--09
Page 2

SVENSKA 3..............................................
DANSK 18................................................
NORSK 33................................................
SUOMI 48................................................
ENGLISH 63..............................................
DEUTSCH 78.............................................
FRANÇAIS 94.............................................
NEDERLANDS 109.........................................
ESPAÑOL 124..............................................
ITALIANO 140..............................................
PORTUGUÊS 155..........................................
ЕЛЛЗНЙКБ 172.............................................
POLSKI 189.................................................
Rätt till ändring av specifikationer utan avisering förbehålles.
Ret til ændring af specifikationer uden varsel forbeholdes.
Rett til å endre spesifikasjoner uten varsel forbeholdes.
Oikeudet muutoksiin pidätetään.
Rights reserved to alter specifications without notice.
Änderungen vorbehalten.
Sous réserve de modifications sans avis préalable.
Recht op wijzigingen zonder voorafgaande mededeling voorbehouden.
Reservado el derecho de cambiar las especificaciones sin previo aviso.
Ci riserviamo il diritto di variare le specifiche senza preavviso.
Reservamo--nos o direito de alterar as especificações sem aviso prévio.
ДйбфзсеЯфбй фп дйкбЯщмб фспрпрпЯзузт рспдйбгсбцюн ЧщсЯт рспейдпрпЯзуз.
Zastrzegamy sobie prawo do wprowadzenia zmian.
-- 2 --
Page 3

ENGLISH
1 DIRECTIVE 64........................................................
2SAFETY 64...........................................................
3 INTRODUCTION 65...................................................
3.1 General 65..................................................................
3.2 Definitions 65................................................................
3.3 Technical data 66............................................................
3.4 Welding method 66...........................................................
3.5 Equipment 67................................................................
4 INSTALLATION 68....................................................
4.1 General 68..................................................................
4.2 Mounting 68.................................................................
4.3 Connections 68..............................................................
5 OPERATION 70.......................................................
5.1 General 70..................................................................
5.2 Starting work 70..............................................................
5.3 Conversion of A6 SFE1 (Submerged arc welding) to MIG/MAG welding 74...........
5.4 Conversion of A6 SFE1 / A6 SFE2 (Submerged arc welding) to Twin--arc 74.........
6 MAINTENANCE 75....................................................
6.1 General 75..................................................................
6.2 Daily 75.....................................................................
6.3 Regularly 75.................................................................
7 FAULT TRACING 76...................................................
8 ACCESSORIES 77....................................................
9 ORDERING OF SPARE PARTS 77......................................
WEAR COMPONENTS 204.................................................
SPARE PARTS LIST 207...................................................
TOCe
-- 6 3 --
Page 4

GB
1DIRECTIVE
DECLARATION OF CONFORMITY
Esab Welding Equipment AB, 695 81 Laxå, Sweden, gives its unreserved guarantee
that automatic welding machine A6 SFE1 / A6 SFE2 / A6 SGE1/ A6 SFE1C from
serial number 740 complies with standard EN 60292, in accordance with the requirements of directive (89/392/EEA) and addendum.
-- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- -- --------
Laxå 97--11--19
Paul Karlsson
Managing Director
Esab Welding Equipment AB
695 81 LAXÅ
SWEDEN Tel: + 46 584 81000 Fax: + 46 584 12336
2SAFETY
Users of ESAB welding equipment have the ultimate responsibility for ensuring that anyone who
works on or near the equipment observes all the relevant safety precautions. Safety precautions
must meet the requirements that apply to this type of welding equipment. The following recommendations should be observed in addition to the standard regulations that apply to the workplace.
All work must be carried out by trained personnel well--acquainted with the operation of the welding
equipment. Incorrect operation of the equipment may lead to hazardous situations which can result
in injury to the operator and damage to the equipment.
1. Anyone who uses the welding equipment must be familiar with:
S its operation
S location of emergency stops
S its function
S relevant safety precautions
S welding
2. The operator must ensure that:
S no unauthorised person is stationed within the working area of the equipment when it is
started up.
S no--one is unprotected when the arc is struck
3. The workplace must:
S be suitable for the purpose
S be free from draughts
4. Personal safety equipment
S Always wear recommended personal safety equipment, such as safety glasses, flame--proof
clothing, safety gloves.
S Do not wear loose--fitting items, such as scarves, bracelets, rings, etc., which could become
trapped or cause burns.
5. General precautions
S Make sure the return cable is connected securely .
S Work on high voltage equipment may only be carried out by a qualified electrician.
S Appropriate fire extinquishing equipment must be clearly marked and close at hand.
S Lubrication and maintenance must not be carried out on the equipment during operation.
ffa9d1ea
-- 6 4 --
Page 5

GB
WARNING
ARC WELDING AND CUTTING CAN BE INJURIOUS TO YOURSELF AND OTHERS. TAKE PRECAUTIONS WHEN WELDING. ASK FOR YOUR EMPLOYER’S SAFETY PRACTICES WHICH SHOULD BE
BASED ON MANUFACTURERS’ HAZARD DATA.
ELECTRIC SHOCK -- Can kill
S Install and earth the welding unit in accordance with applicable standards.
S Do not touch live electrical parts or electrodes with bare skin, wet gloves or wet clothing.
S Insulate yourself from earth and the workpiece.
S Ensure your working stance is safe.
FUMES AND GASES -- Can be dangerous to health
S Keep your head out of the fumes.
S Use ventilation, extraction at the arc, or both, to take fumes and gases away from your breathing zone
and the general area.
ARC RAYS -- Can injure eyes and burn skin.
S Protect your eyes and body. Use the correct welding screen and filter lens and wear protective
clothing.
S Protect bystanders with suitable screens or curtains.
FIRE HAZARD
S Sparks (spatter) can cause fire. Make sure therefore that there are no inflammable materials nearby.
NOISE -- Excessive noise can damage hearing
S Protect your ears. Use earmuffs or other hearing protection.
S Warn bystanders of the risk.
MALFUNCTION -- Call for expert assistance in the event of malfunction.
READ AND UNDERSTAND THE INSTRUCTION MANUAL BEFORE INSTALLING OR OPERATING.
PROTECT YOURSELF AND OTHERS!
3 INTRODUCTION
3.1 General
All the automatic welding machines included in this instruction manual are designed
for SAW and MIG/MAG welding of butt and fillet joints.
ESAB’s welding heads are of the A6 S type and are intended for use in combination
with A2--A6 Process Controller and ESAB’s welding power sources LAF and T A F.
The welding head can be positioned horizontally and vertically with the linear slides.
The angular position is adjusted with the angular slide.
3.2 Definitions
SAW welding The weld bead is protected by a cover of flux during the
welding.
SAW Heavy duty Permits welding with high current load and thick wire.
SAW Light duty Permits welding with low current load and thin wire.
MIG/MAG welding The weld bead is protected by shielding gas during wel-
ding.
Tandem welding Welding with two welding heads.
Twinarc welding Welding with two wires in the same welding head.
ffa9d1ea
-- 6 5 --
Page 6

GB
3.3 Technical data
A6 SFE1 A6 SFE1 A6 SFE2 A6 SGE1 A6 SFE1C
UP UP UP MIG/MAG UP
LD D20 HD D35 HD D35
Rated load 100%
60 %
Wire dimensions:
solid single wire 1.6--4.0 mm 3.0--6.0 mm 3.0--6.0 mm 0.8--2.5 mm -- 4 . 0 m m
flux--cored wire 1.6--4.0 mm 3.0--4.0 mm -- 1.2--3.2 mm -twin wire 2x1.2--2.0 mm 2x2.0--3.0mm 2x2.0--3.0mm -- --
Wire feed speed 0.2--4.0 m/min 0.2--4.0 m/min 0.2--4.0 m/min 0.2--15 m/min 0.2--4.0 m/min
Brake drum braking torque 1.5 Nm 1.5 Nm 1.5 Nm 1.5 Nm 1.5 Nm
Max weight, wire 2x30 kg 2x30 kg 4x30 kg 30 kg 2x30 kg
Flux hopper capacity
(Must not be filled with preheated
flux)
Weight (flux and wire excluded) 50 kg 50 kg 100 kg 15 kg 50 kg
Sideways tilt, max. 25_ 25_ 25_ 25_ 25_
Setting length of slide *
manual
motor--driven (with ball bearings)
Continuous A--weighted noise pressure
800 A
1000 A
AC/DC
10 l 10 l 10 l -- 1l
210 mm
300 mm
68 dB 68 dB 68 dB 83 dB 68 dB
1500 A
--
AC/DC
210 mm
300 mm
1500 A
--
AC/DC
210 mm
300 mm
600 A
--
AC/DC
210 mm
300 mm
1500 A
--
AC/DC
60 mm
*) NB! Other lengths on request.
3.4 Welding method
Submerged arc welding (SAW)
For SAW welding the A6 SF welding head is always used. It is available in the
following designs:
S Submerged--arc Light duty
Submerged--arc light duty, with a ∅ 20 mm connector, which permits a load of up
to 800 A (100%) or 1000 A (60%).
S Submerged--arc Heavy duty
Submerged--arc heavy duty, with a ∅ 35 mm connector, which permits a load of
up to 1500 A.
Both versions can be equipped with feed rollers for single or twin wire welding (twin-arc). A special knurled feed roller is available for flux--cored wire, which guarantees
even wire feed without the r isk of deformation due to high feed pressure.
For work in confined spaces, (smaller than 50 cm), a special welding head of type
A6 SFE1C is available, which can be installed on the Mastertrac as required.
Tandem welding (submerged--arc)
For tandem welding, a welding head of type A6 SFE2 is always used, which must be
connected to 2 welding power sources and 2 control boxes of type A2 --A6 Process
Controller.
The tandem welding head includes 2 single welding heads (A6 SF), each with its
own contact tip. Each contact tip has a m aximum rated load of 1500 A.
ffa9d1ea
-- 6 6 --
Page 7
GB
MIG/MAG welding
For MIG/MAG welding the A6 SG welding head is always used, permitting a max.
load of 600 A. The welding head is water--cooled, with the cooling water supplied by
hoses from connections intended for the purpose.
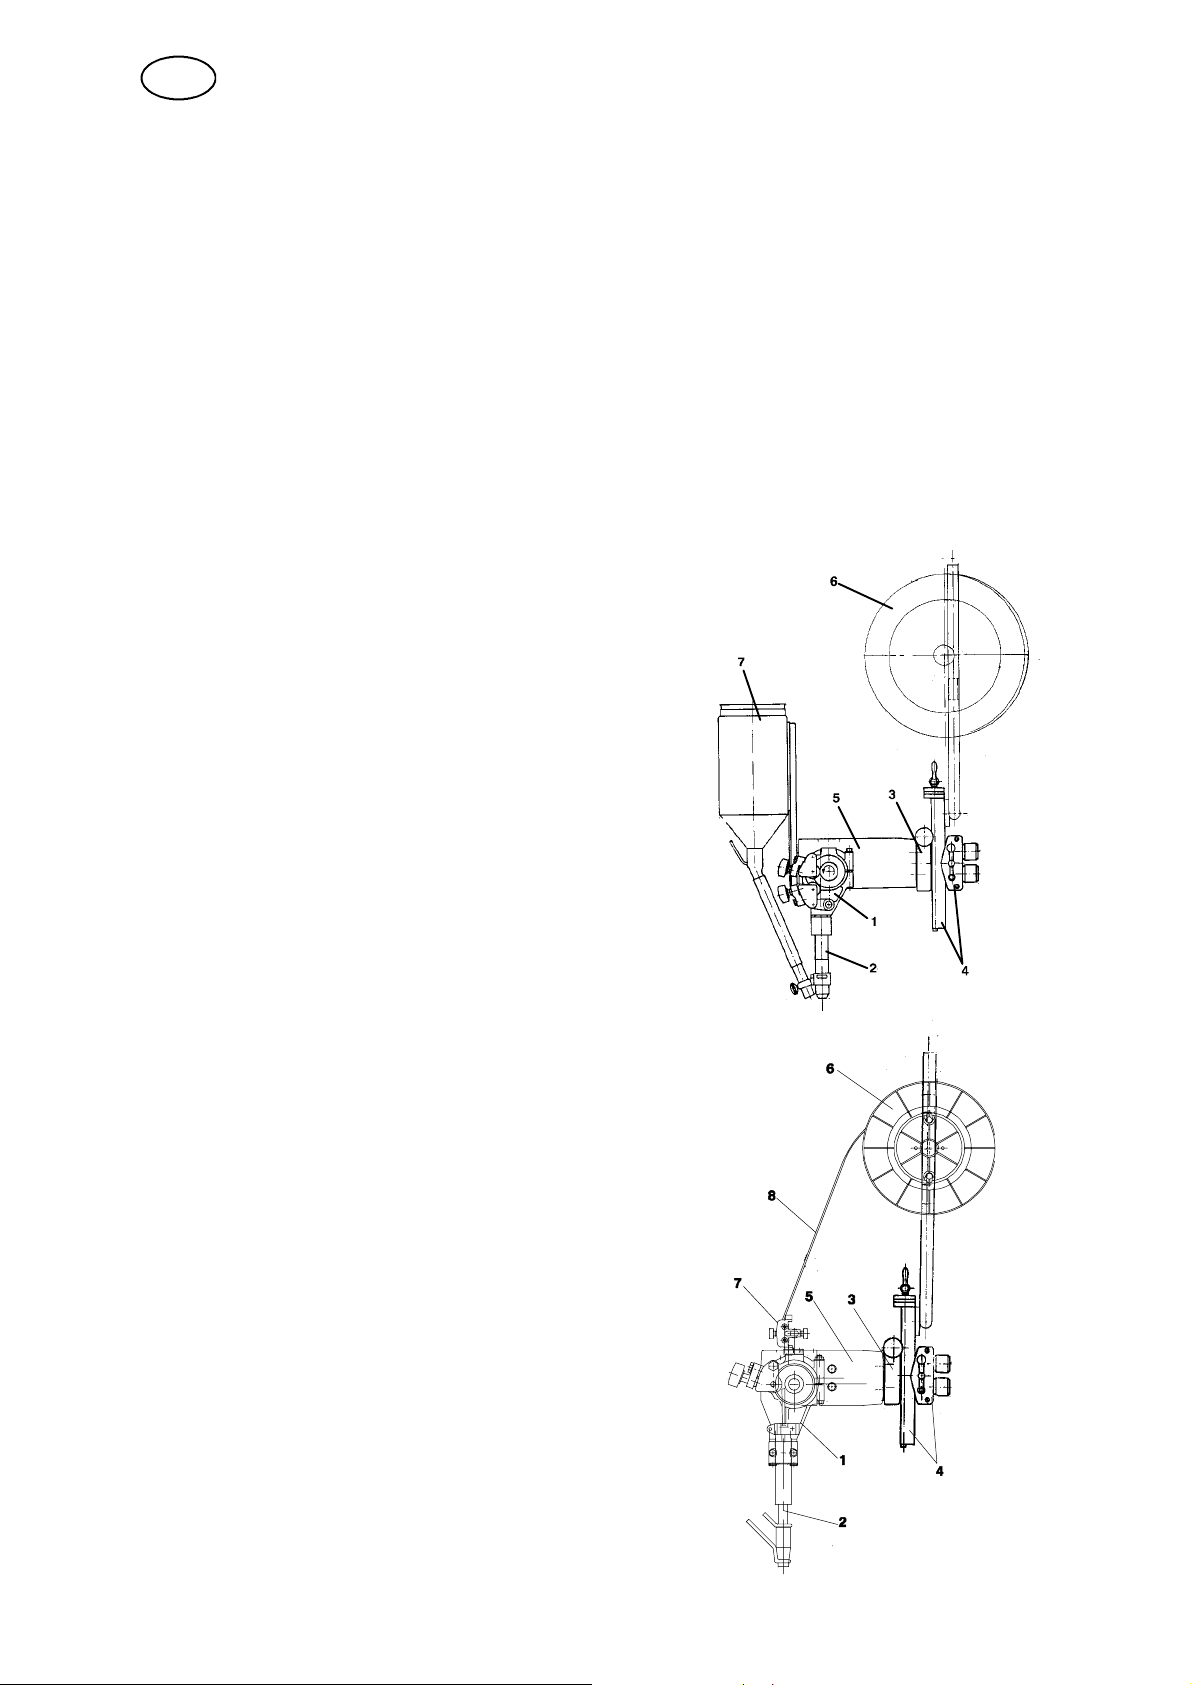
3.5 Equipment
Included in a complete welding head are a feed motor (A6 VEC) to feed in the wire
and contact equipment which supplies current to the wire and provides a good contact.
Contact equipment is available in several different versions.
S A6 SF is used for submerged--arc welding.
S A6 SG is used for MIG/MAG welding.
Example -- A6 SFE1 and A6 SFE2
1 Straightener.
2 Contact equipment which consists of a
contact tip, connector and flux tube.
3 Angular slide
4 Slide (motor--driven or manually operated)
5 Motor and gearbox (A6 VEC)
6 Wire drum
7 Flux hopper (may be fitted with a cyclone)
Example -- A6 SGE1
1 Straightener.
2 Contact equipment which consists of a
connector, gas nozzle and water hoses.
3 Angular slide.
4 Slide (motor--driven or manually operated)
5 Motor and gearbox (A6 VEC).
6 Wire drum.
7 Fine--wire straightener (Accessories).
8 Wire guide.
ffa9d1ea
-- 6 7 --
Page 8
GB
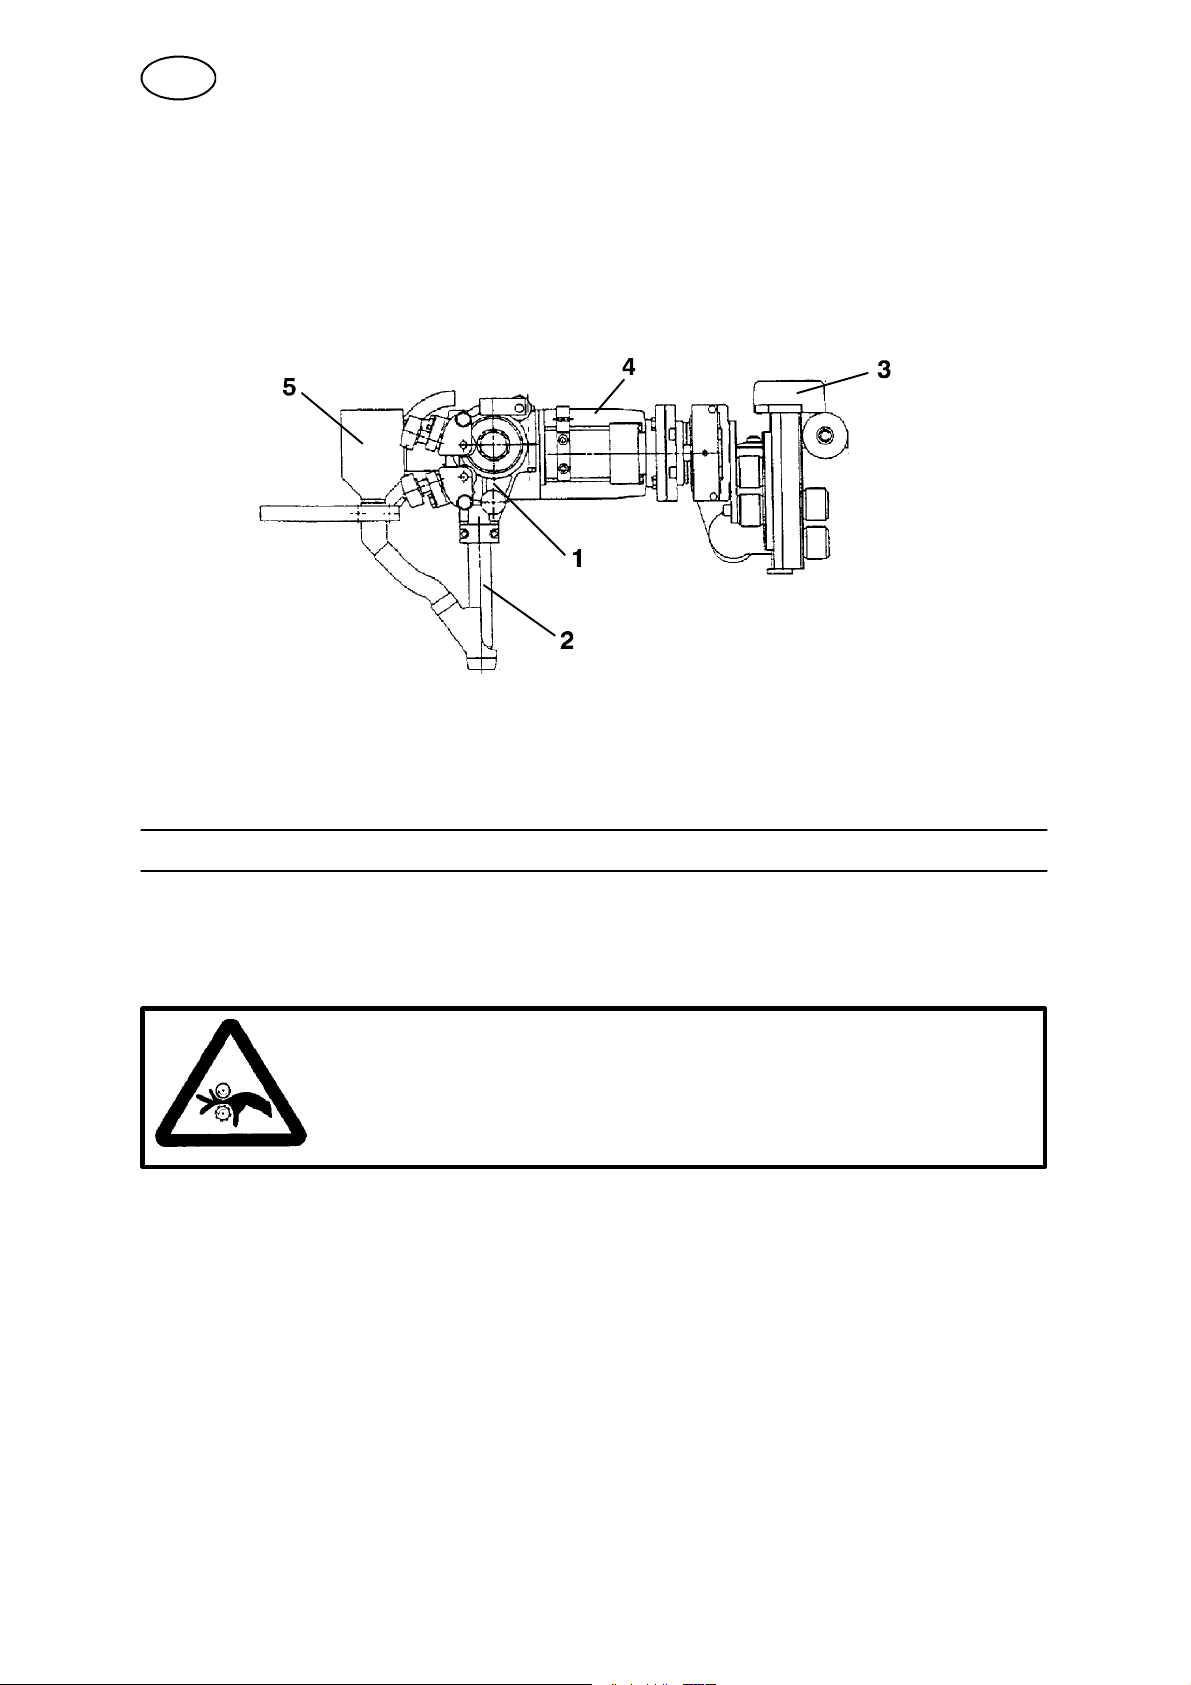
Example of the A6 SFE1C
1 Straightener.
2 Contact equipment, which consists of a contact tip, connector and flux tube.
3 Slide (motor--driven).
4 Motor and gearbox (A6 VEC).
5 Flux hopper (1 l).
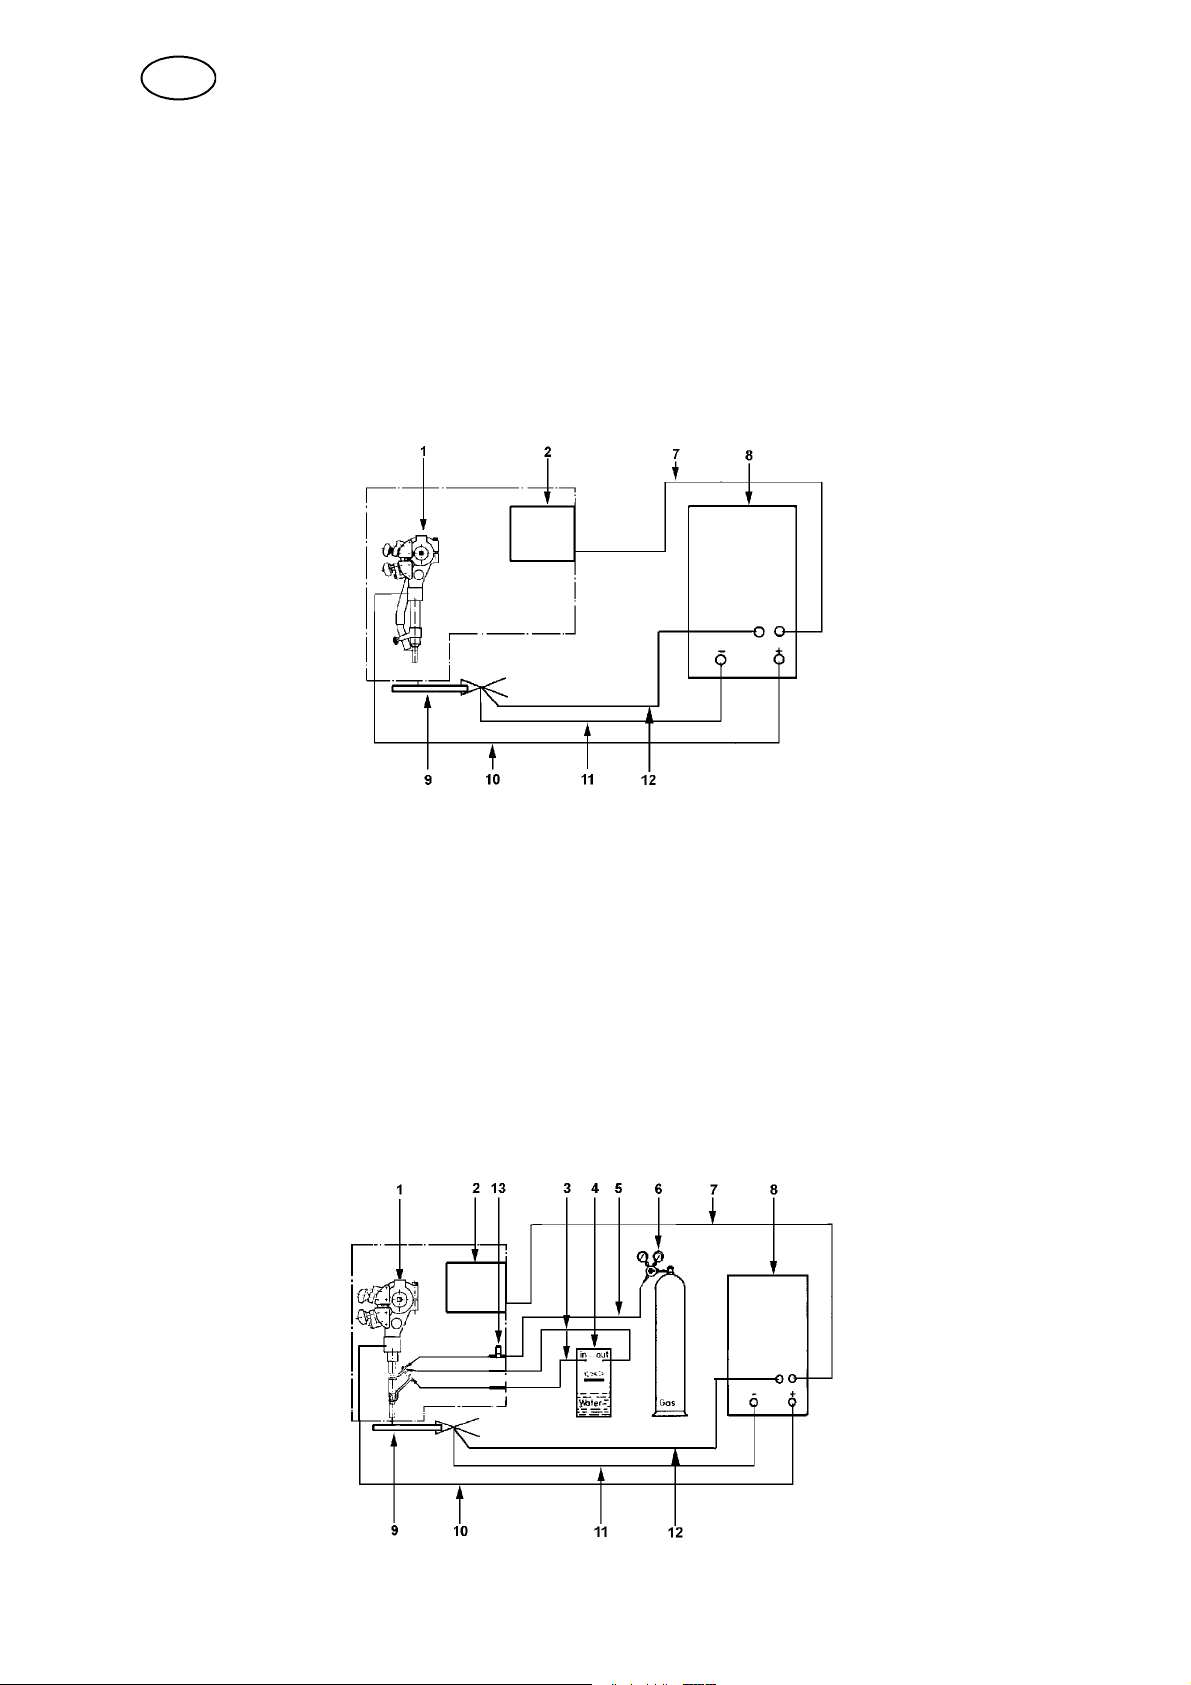
Connection instructions for SAW and MIG/MAG welding appear from the system diagram on page 69.
4 INSTALLATION
4.1 General
Installation shall only be performed by qualified personnel.
WARNING
Rotating parts can cause injury, take great care.
4.2 Mounting
The automatic welding machines can easily be fitted with 4 screws M 10x40 on a
rail--borne carriage or on a column and boom unit.
4.3 Connections
1. The connection of the A2--A6 Process Controller (PEH) to the welding machine
shall be done according to the connection instructions in the A2--A6 Process
Controller (PEH) service manual.
For further information, see instruction manual for the A2--A6 Process Controller
(PEH).
ffa9d1ea
-- 6 8 --
Page 9
GB
2. Connect the A6 welding heads as follows:
SUBMERGED ARC WELDING (SAW)
S Connect the control cable (7) between the welding power source (8) and the
A2--A6 Process Controller (PEH) (2).
S Connect the return cable (11) between the welding power source (8) and the
work piece (9).
S Connect the welding cable (10) between the welding power source (8) and
the automatic welding machine (1).
S Connect the measuring cable (12) between the welding power source (8)
and the work piece (9).
GAS METAL ARC WELDING (MIG/MAG)
S Connect the control cable (7) between the welding power source (8) and the
A2--A6 Process Controller (PEH) (2).
S Connect the return cable (11) between the welding power source (8) and the
work piece (9).
S Connect the welding cable (10) between the welding power source (8) and
the automatic welding machine (1).
S Connect the gas hose (5) between the reduction valve (6) and the gas valve
on the automatic welding machine (13).
S Connect the hoses for cooling water (3) between the cooling unit (4) and the
automatic welding machine (1).
S Connect the measuring cable (12) between the welding power source (8)
and the work piece (9).
ffa9d1ea
-- 6 9 --
Page 10
GB
5 OPERATION
5.1 General
General safety regulations for the handling of the equipment can be found on
page 64. Read through before you start using the equipment!
S Select wire type and flux or shielding gas so that the weld material is as close as
possible to the analysis of the base metal. Select wire size and welding data in
accordance with the values recommended by the welding materials supplier.
S Thorough preparation of the weld surfaces is necessary to achieve a good weld.
NOTE! The width of the weld joint gap must be uniform.
S To minimise the risk of heat crack formation, the width of the weld must be
greater than the penetration depth.
S Always carry out a test weld with the same joint type and sheet thickness as the
production work piece.
S For control and adjustment of the automatic welding machine and welding power
supply, see the instruction manual for the A2--A6 Process Controller (PEH).
S For replacement of wear parts, see table on page 204.
5.2 Starting work
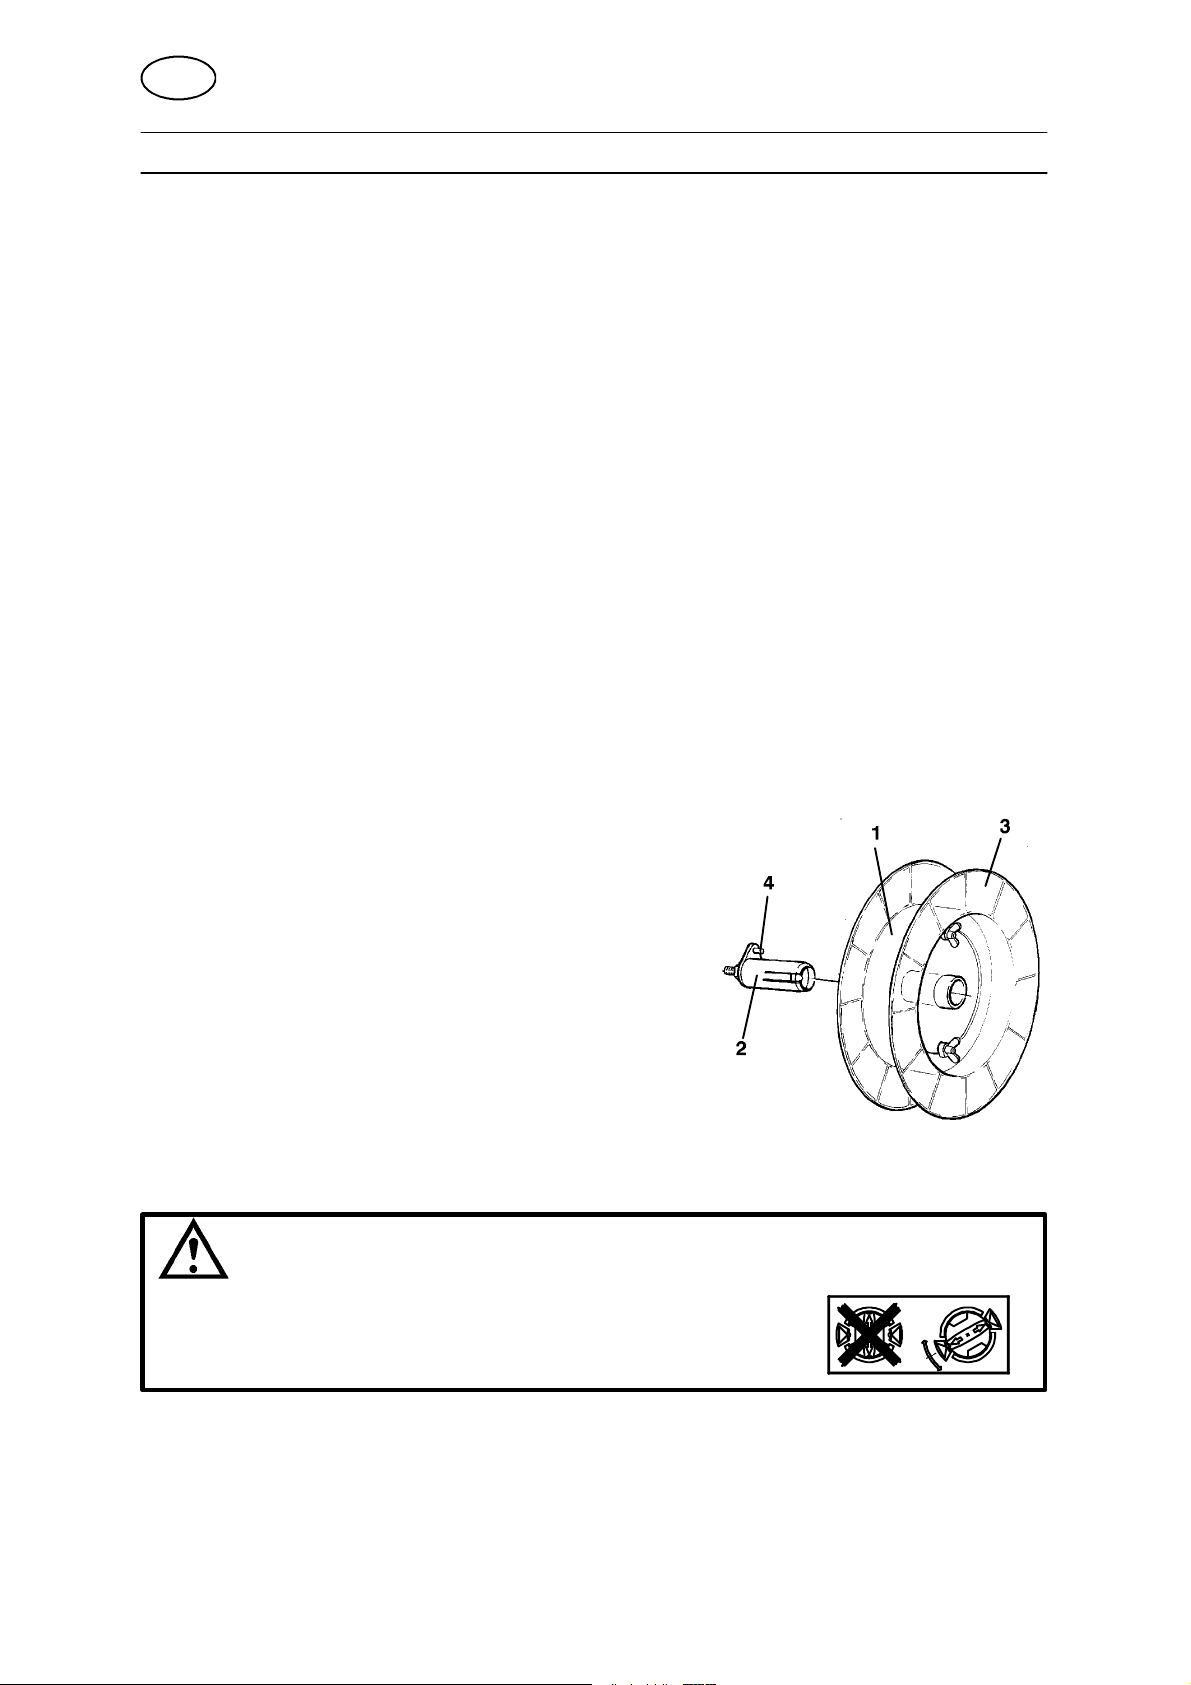
Loading the welding wire
S Remove the wire drum (1) from the brake hub (2)
and take off the side plate (3).
S Locate the wire reel on the wire drum (1).
S Cut off the binding wires from around the
wire reel.
S Fit the side plate (3).
S Fit the wire drum (1) on the brake hub (2).
Check that the carrier (4) is in the correct position.
NOTE! The maximum angle for the wire bobbin is 25°.
At extreme angles, wear will occur on the brake hub locking
mechanism and the wire bobbin will slide off the brake hub.
WARNING
To prevent the r eel sliding off the hub:
S
Lock the reel in place by turning the red knob as shown
on the warning label attached next to the hub.
ffa9d1ea
-- 7 0 --
Page 11
GB
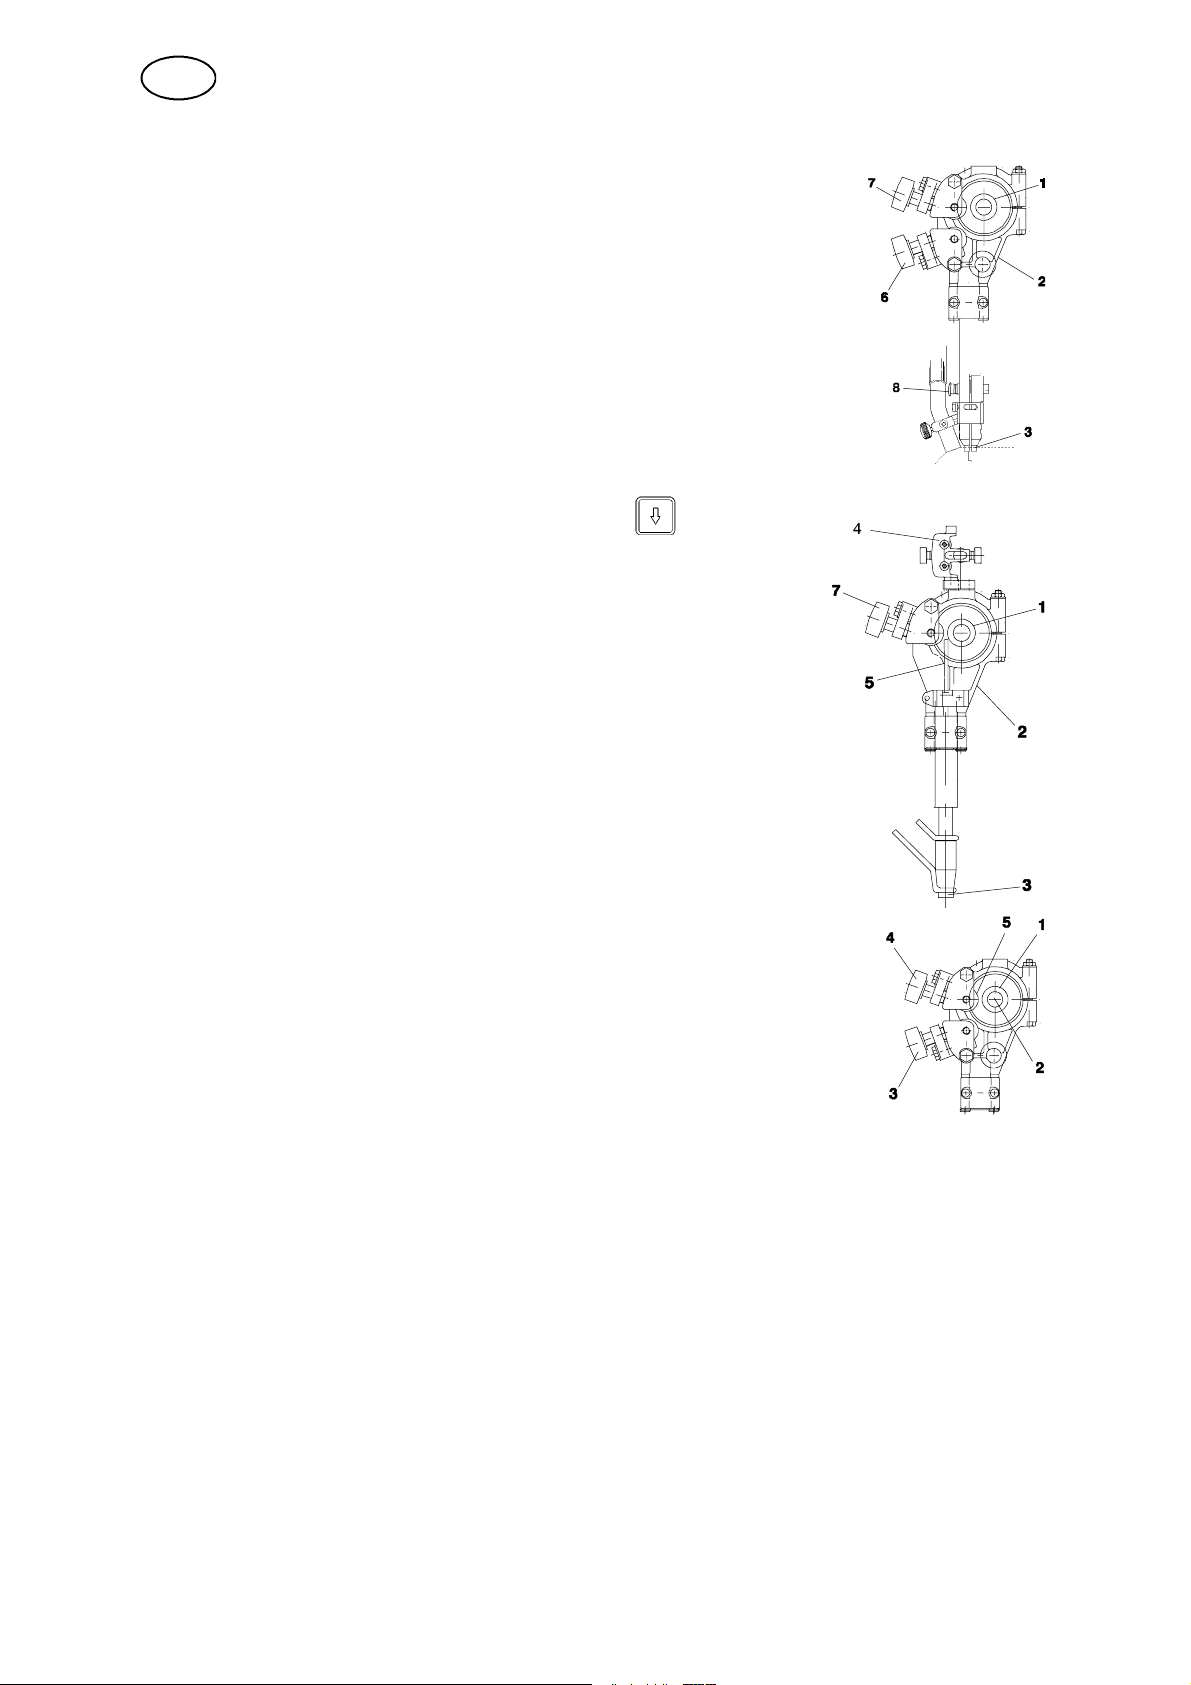
S Check that the feed roller (1) and contact jaw or contact tip
(3) are of the correct dimension for the selected wire size.
S Pull the end of the wire through the straightener (2). For a
wire diameter greater than 2 mm; straighten out 0.5 m of
wire and feed it by hand down through the straightener.
S Locate the end of the wire in the feed roller (1) groove.
S Set the wire tension on the feed roller with the knob (7).
Note! Do not tension more than is required to achieve an
even feed.
S The pressure screw (8) must not be dismantled. (Applies to
Submerged--arc Heavy duty).
S Feed the wire forward 30 mm by pressing on the
control box A2--A6 Process Controller.
S Direct the wire by adjusting the knob (6).
For fine wire, the special fine wire straightener (4) is used
for both single and twin wire.
Ensure that the straightener is correctly adjusted so that the
wire emerges straight out through the contact jaws or
contact tip.
SAW
MIG/MAG
Always use a guide tube (5) to ensure even feeding of fine
wire (1.6 -- 2.5 mm).
For MIG/MAG welding with wire sizes < 1.6 mm, use a
guide spiral, which is inserted in the guide tube (5).
Changing the feed roller
S Single wire
S Release the knobs (3) and (4).
S Release the hand wheel (2).
S Change the feed roller (1). The rollers are marked with
their respective wire sizes.
S Twin wire (Twin--arc)
S Change the feed roller (1) with twin grooves in the same way as for single
wire.
S NOTE! The pressure roller (5) must also be changed. A special spherical
pressure roller for twin wire replaces the standard pressure roller for single
wire.
S Assemble the pressure roller with special stub shaft
(order no. 146 253--001).
S Flux--cored wire (for knurled rollers)
S Change the feed roller (1) and pressure roller (5) in pairs for the wire size to
be used. NOTE! A special stub shaft is r equired for the pressure roller
(order no. 0212 901 101).
S Tighten the pressure screw (4) with moderate pressure to ensure that the
flux--cored wire does not deform.
ffa9d1ea
-- 7 1 --
Page 12
GB
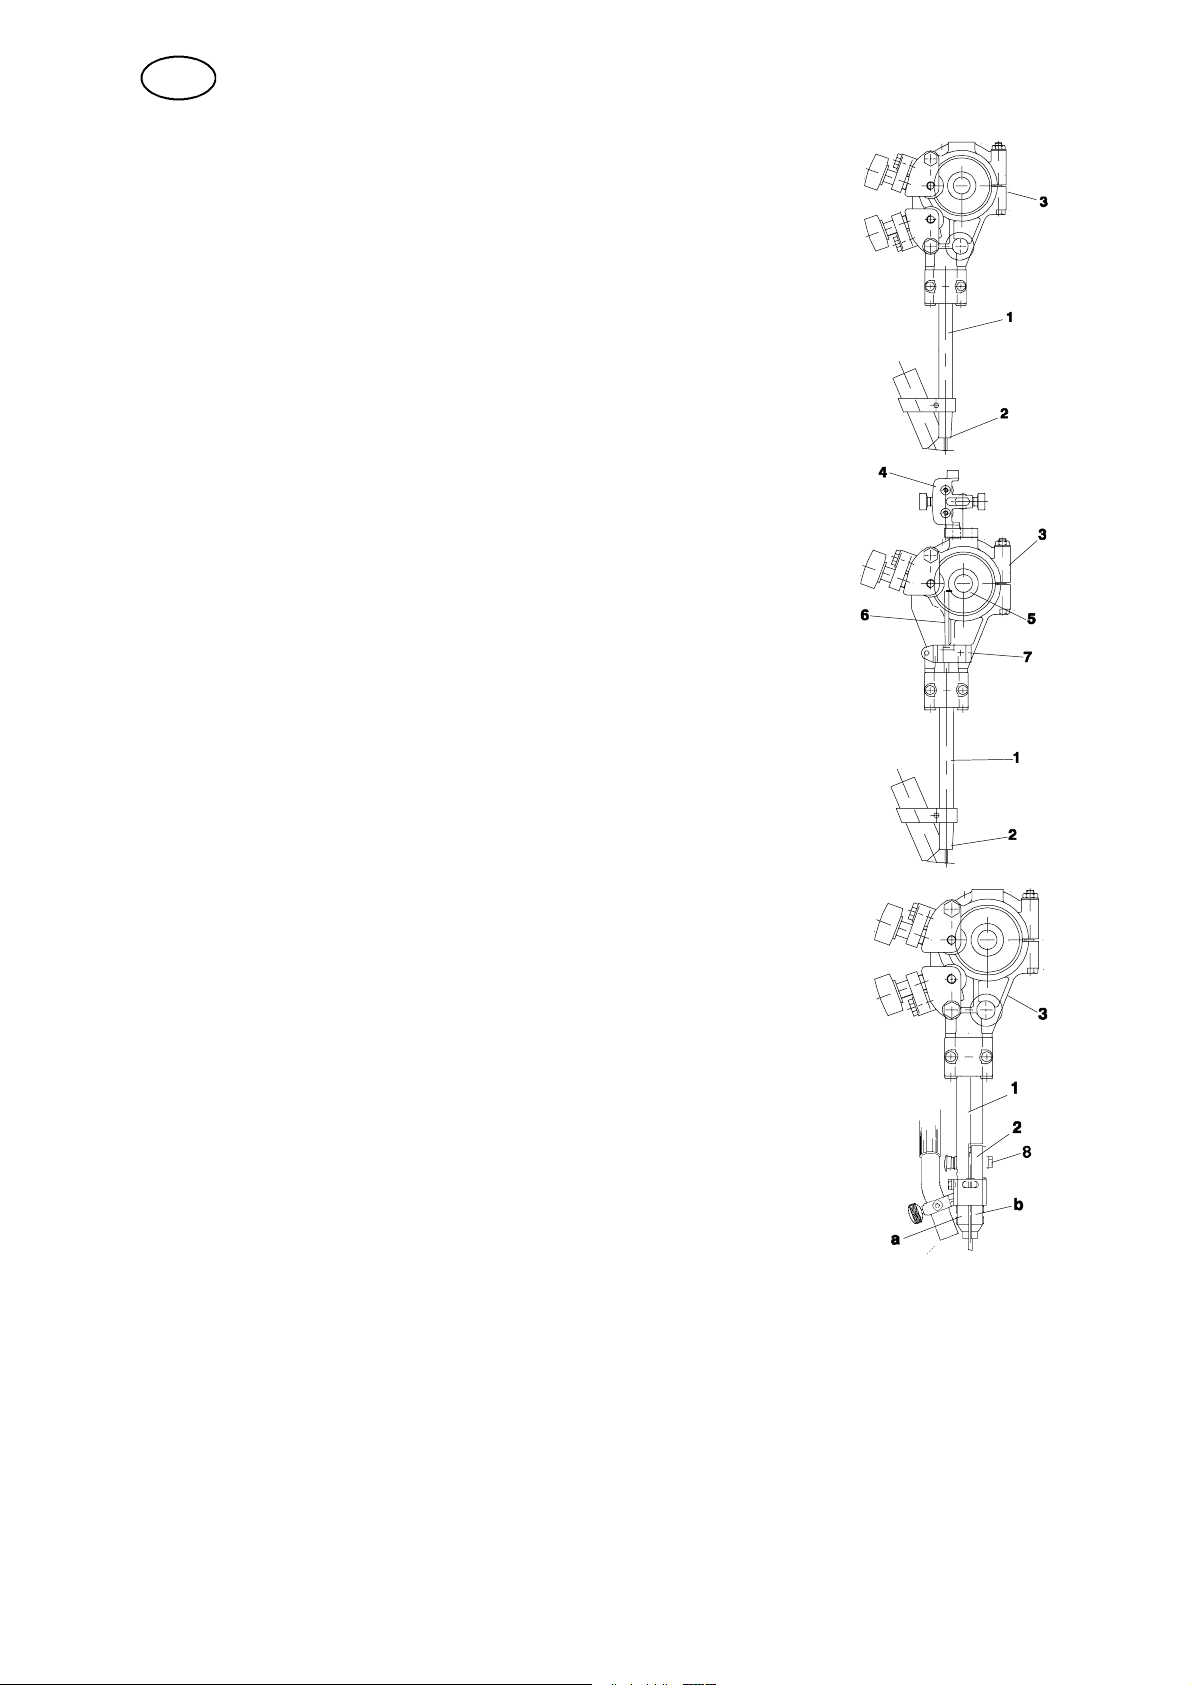
Contact equipment for submerged--arc welding
S For single wire 3.0 -- 4.0 mm. Light duty (D20)
Use the straightener (3), connector (1) D20 with contact tip (2)
(M12 thread).
S Tighten the contact tip (2) with a key in order to ensure
that a good contact is achieved.
S For single wire 1.6 -- 2.5 mm Submerged--arc.
Light duty (D20)
Use the straightener (3), connector (1) D20 with contact
tip (2) (M12 thread) and separate fine wire straightener (4)
with guide tube (6).
S Fit the clamp (7) with guide tube (6) in the M12 hole on
the straightener (3). The guide tube (6) should bottom
on the contact tip (2).
S If necessary, cut the guide tube (6) to length so that the
feed roller ( 5) runs freely.
S Fit the fine wire straightener (4) on the upper side of the
clamp for the straightener (3).
S For single wire 3.0 -- 6.0 mm. Heavy duty (D35)
Use the straightener (3), connector (1) D35 with contact
jaws (2).
S Fit one of the contact jaws with the M5 bolts provided, in
the fixed contact tip (a).
S Fit the other contact jaw in the free half of the two--piece
connector (b) under the bolt (8) and tighten down hard to
ensure that a good contact is achieved between the
contact jaws and the wire.
S For flux--cored wire 1.6 mm -- 4.0 mm (D20 and D35) (Accessories)
If contact jaws (D35) are used, the contact jaws must not be tightened too hard
in order that the flux--cored wire is not deformed. Ensure that good contact is
achieved with the wire.
S Adjustment of the wire for tandem welding
S The distance between the first and second wire must not be so great that the
slag gets time to solidify between the wires.
S Ensure that good flux coverage is achieved between the first and second
wires.
ffa9d1ea
-- 7 2 --
Page 13
GB
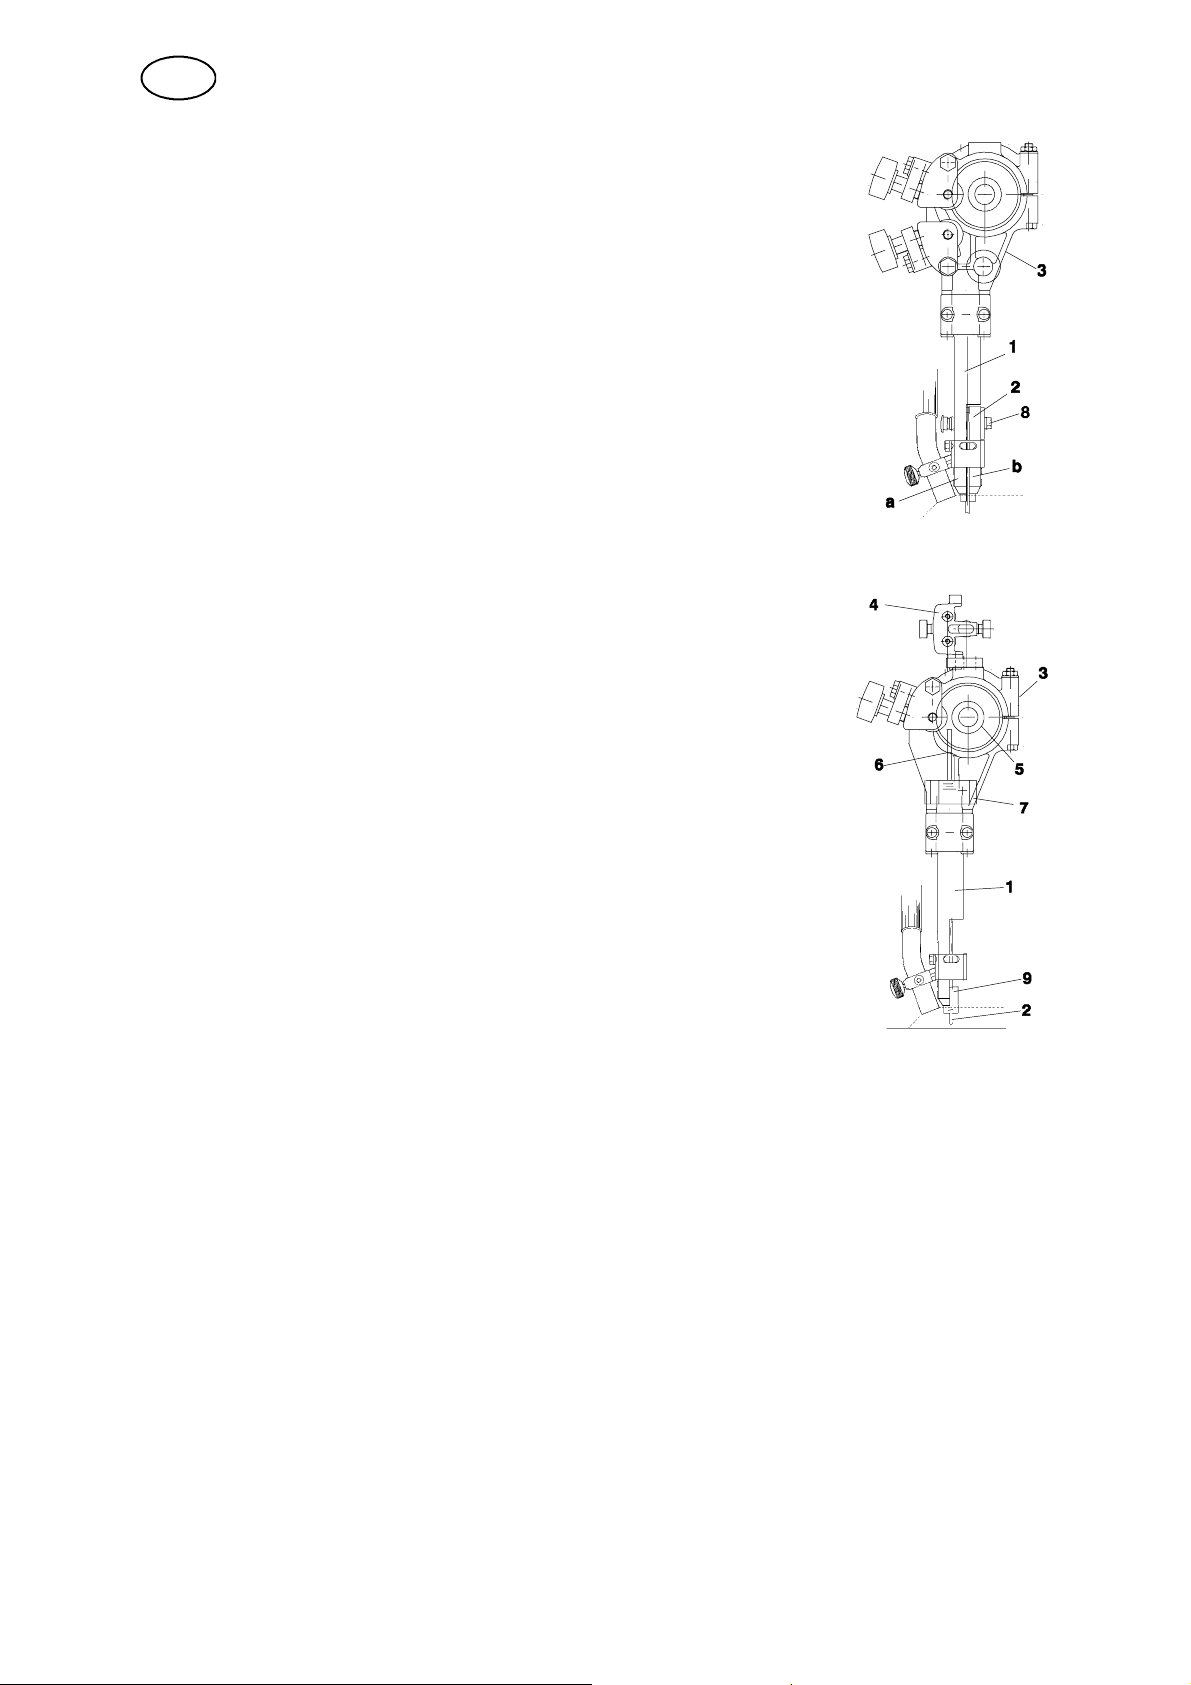
S Fortwinwires2x2.0--3.0Heavy Twin (D35) (Accessories)
Use the straightener (3), connector (1) D35 with contact
jaws (2).
S Fit the first contact jaw with the M5 bolts supplied, in the
fixed connector (a).
S Fit the other contact jaw in the free half of the two--piece
connector (b) under the bolt (8) and tighten down hard to
ensure that a good contact is achieved between the
contact jaws and the wire.
S Fortwinwire2x1.2--2.0mm,LightTwin(D35)(Accessories)
Use the straightener (3), connector (1) D35 with twin
adapter (9) and 2 contact tips (2) (M6 threads) and separate
fine wire straightener (4) with two guide tubes (6). For twin
wire < 1.6 mm, insert a guide spiral into each guide tube.
S Fit the twin adapter (9) for M6 contact tips (2) with the
M5 bolts in the fixed half of the two--piece connector
(1).
S Fit the clamp (7) with guide tube (6) in the M12 hole on
the standard straightener (3). The guide tube should
bottom on the twin adapter (9) for the contact tip (2).
S Tighten the contact tip (2) with a key to ensure that a
good contact is achieved.
S If necessary, cut the guide tube (6) to length so that the
feed roller ( 5) runs freely.
S Adjustment of the wires for Twin--arc welding:
S Position the wires in the joint so as to achieve optimal weld quality by
rotating the connector. The two wires can be rotated so that they are
positioned one after the other along the line of the joint, or in any position
up to 90˚ across the joint, i.e. one wire on e ach side of the joint.
ffa9d1ea
-- 7 3 --
Page 14
GB
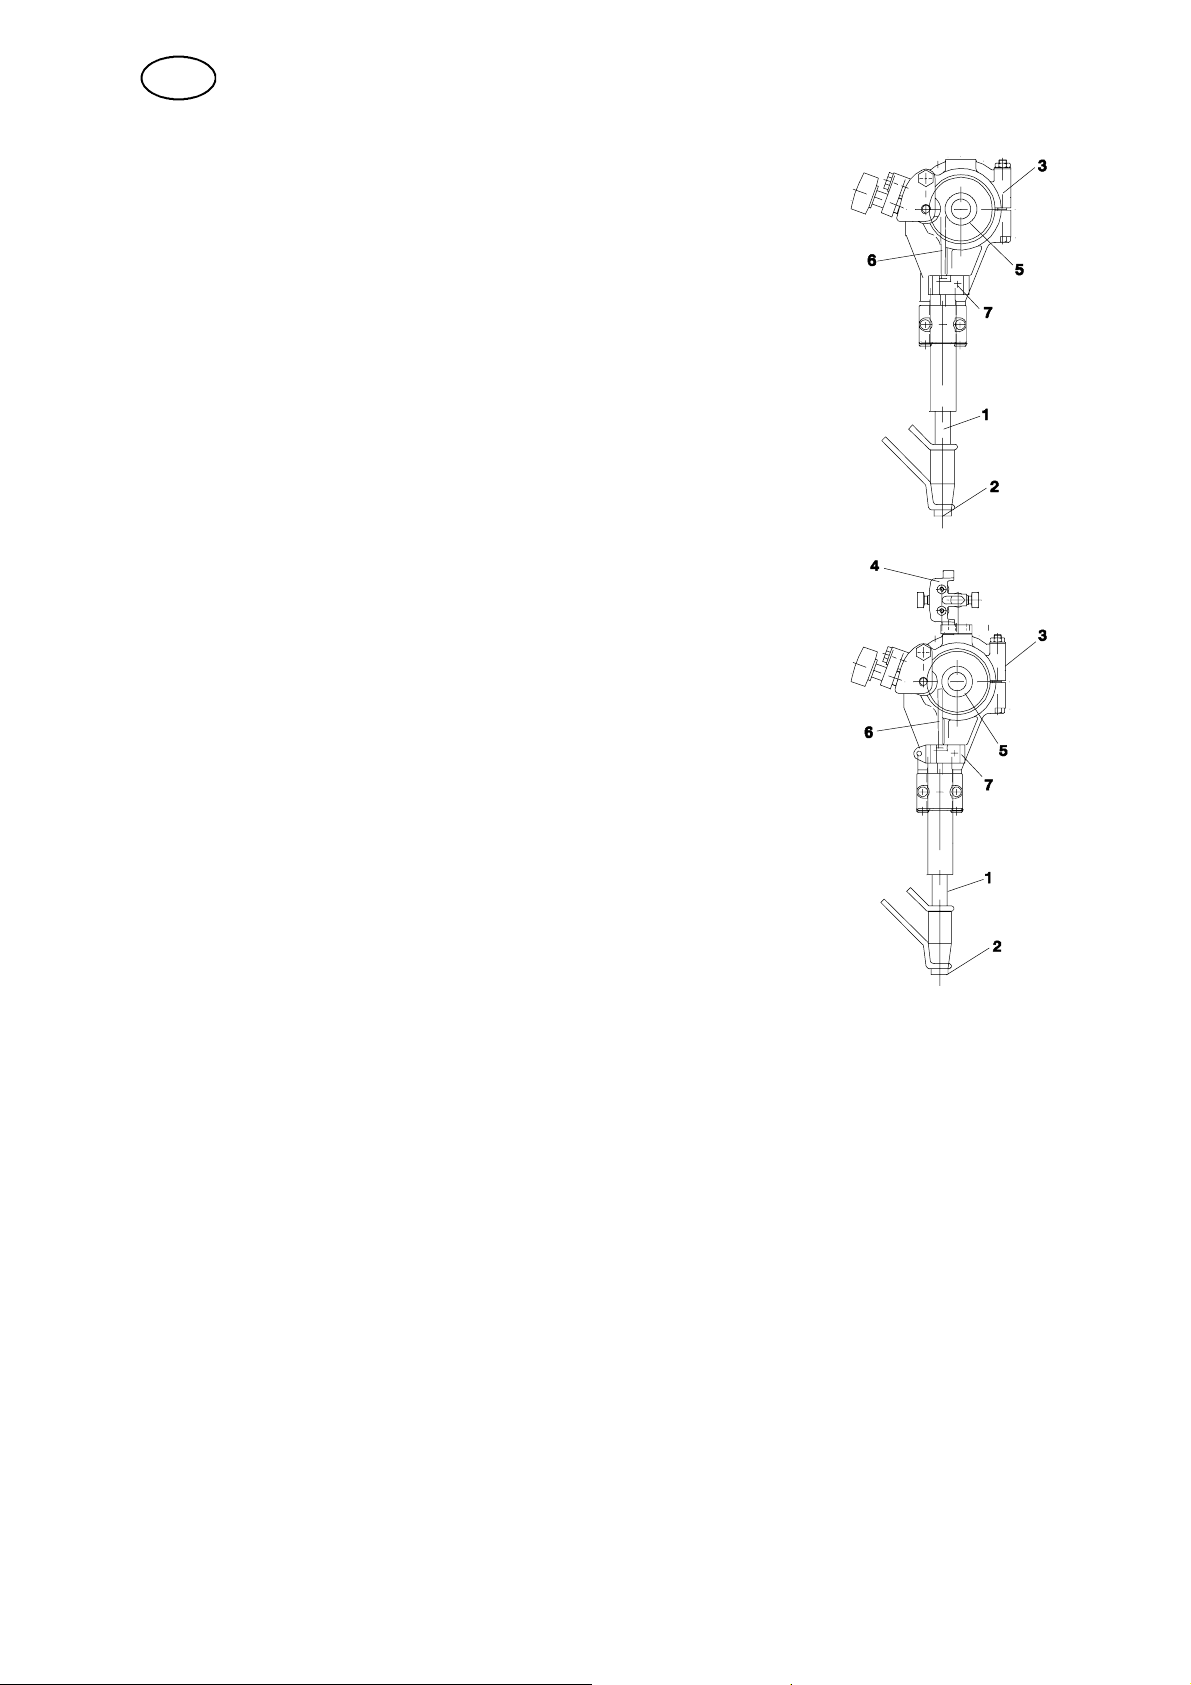
Contact equipment for MIG/MAG welding.
S For single wire 1.6 -- 2.5 mm (D35)
Use the straightener (3), connector (1) D35 with contact
tip (2) (M10 thread).
S Tighten the contact tip (2) with a key to ensure that a
good contact is achieved.
S Fit the clamp (7) with guide tube (6) in the M12 hole on
the standard straightener (3). The guide tube (6) should
bottom on the contact tip (2).
S If necessary, cut the guide tube (6) to length so that the
feed roller ( 5) runs freely.
S For single wire < 1.6 mm (D35)
Use the straightener (3), connector (1) D35 with contact tip (2)
(M12 thread), fine wire straightener (4) with guide tube (6)
and guide spiral, which is inserted in the guide tube (6).
S Fit the clamp (7) with guide tube (6) in the M12 hole on
the standard straightener (3). The guide tube (6) should
bottom on the contact tip (2).
S If necessary, cut the guide tube (6) to length so that the
feed roller ( 5) runs freely.
S Fit the fine wire straightener (4) on the upper side of the
clamp for the straightener (3).
S Connect the cooling water and gas (MIG/MAG welding).
Filling o f flux ( Sub merged arc welding)
S Close the flux valve on the flux hopper.
S Remove the cyclone on the flux recovery unit, if fitted.
S Fill with flux . NOTE! The flux must be dry. If possible, avoid using agglomerating
flux outdoors and in a damp environment.
S Position the flux tube so that the flux hose does not become kinked.
S Adjust the height of the flux nozzle above the weld so that the correct amount of
flux is delivered.
The flux coverage should be high enough to prevent the arc from burning
through.
5.3 Conversion of A6 SFE1 (Submerged arc welding) to MIG/MAG
welding
Assemble the conversion kit according to the instructions provided.
5.4 Conversion of A6 SFE1 / A6 SFE2 (Submerged arc welding) to
Twin--arc
Assemble the conversion kit according to the instructions provided.
ffa9d1ea
-- 7 4 --
Page 15
GB
6 MAINTENANCE
6.1 General
NB! Before doing any kind of maintenance work, make sure the mains is discon-
nected.
For the maintenance of the A2--A6 Process Controller (PEH), see the instruction
manual.
6.2 Daily
S Clean flux and dirt off moving parts of the welding machine.
S Check that the contact tip and all electric cables are connected.
S Check that all bolted joints are tight and that guides and drive rollers are not
worn or damaged.
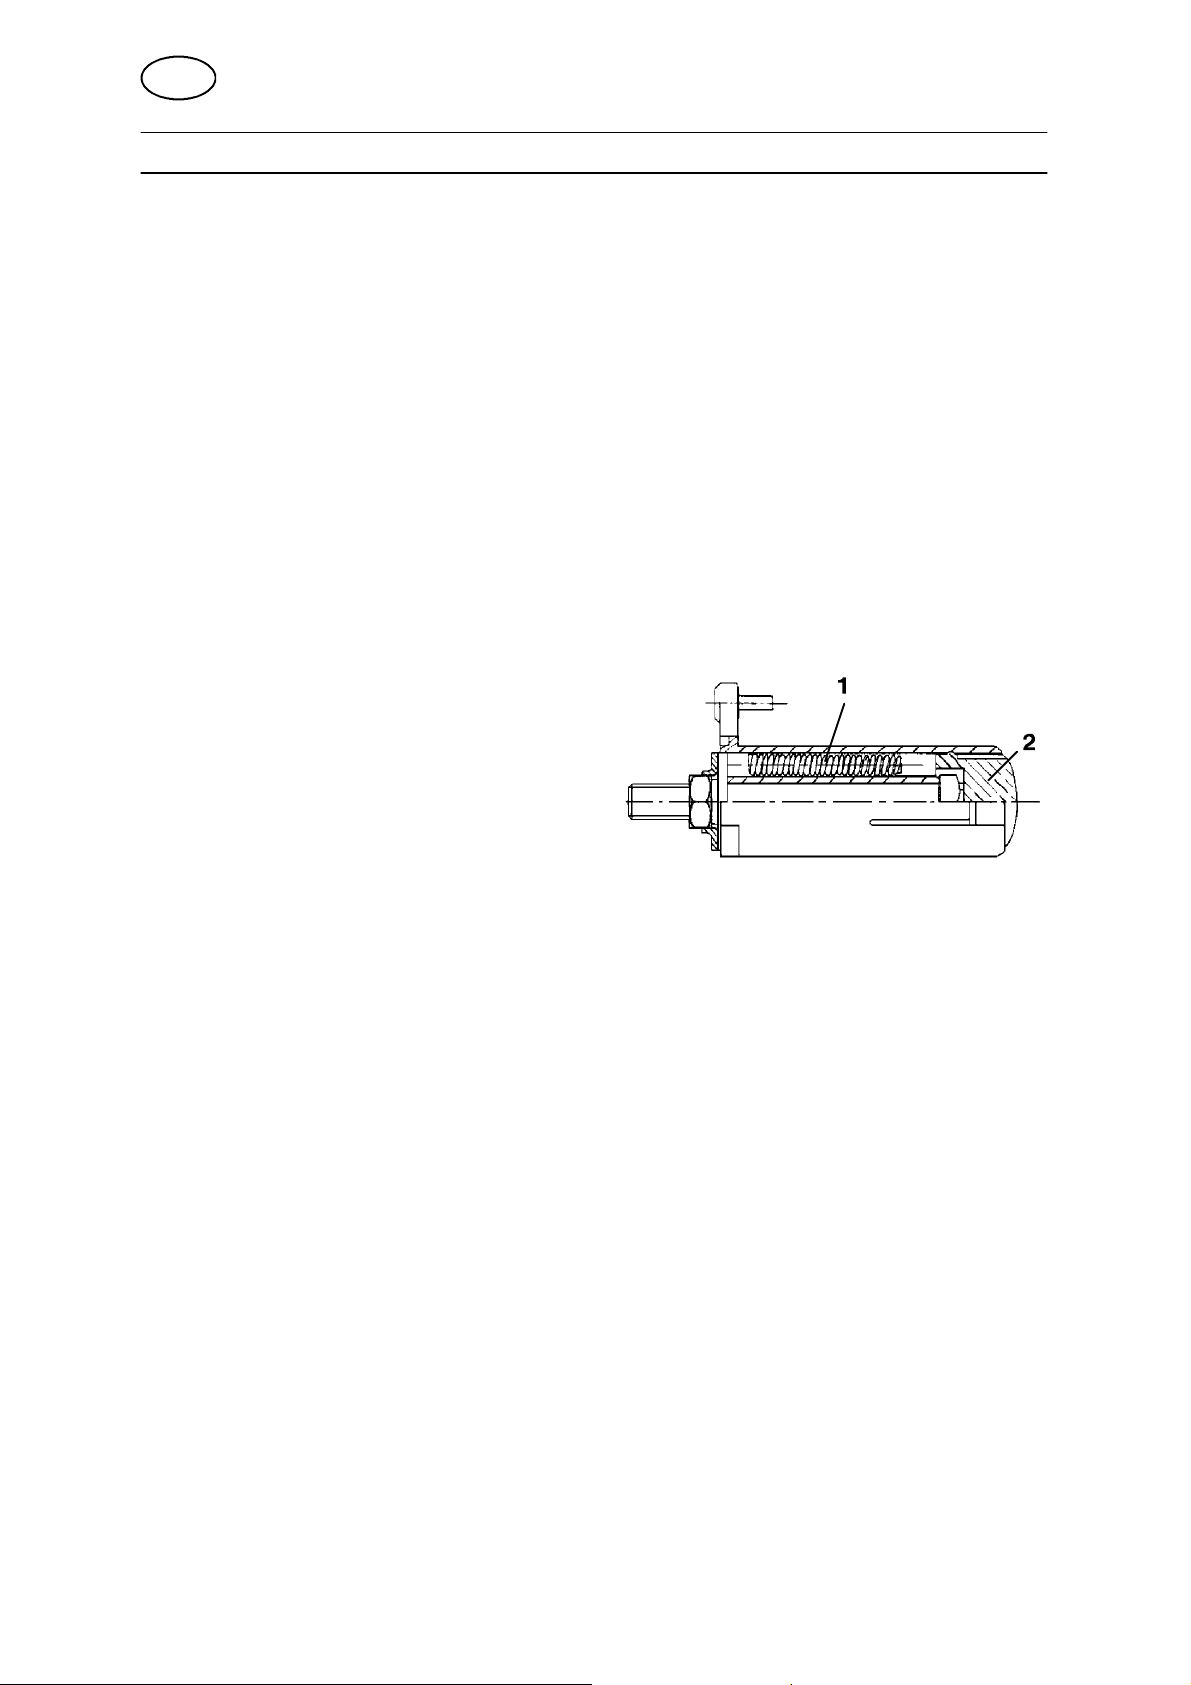
S Check the brake hub braking torque. It should not be so low, that the wire reel
continues to rotate when wire feed is stopped, and it should not be so great that
the feed rollers slip. As a guide, the braking torque for a 30 kg wire reel should
be 1.5 Nm.
Adjusting the braking torque:
S Set the locking button (2) to the
locked position.
S Insert a screwdriver into the hub
springs.
S Turning the springs (1) clockwise
reduces the braking torque.
S Turning the springs anticlockwise increases the torque.
NOTE! Turn the springs by the same amount.
6.3 Regularly
S Check the carbon brushes of the wire feed motor every three months. Replace
when they are worn down to 6 mm.
S Check the slides and lubricate if they bind.
S Check the wire guides, drive rollers and contact tip of the wire feed unit.
Replace any worn or damaged components, (see spare parts list on page 207).
ffa9d1ea
-- 7 5 --
Page 16
GB
7 FAULT TRACING
Equipment S Instruction manual for control box A2--A6 Process Controller.
S Operating manual for motor with gear A6 VEC,
order no. 0443 393.
Check S that the power source is connected for the correct mains supply
S that all three phases are live ( phase sequence is not important)
S that welding cables and connections are not damaged
S that the controls are correctly set
S that the mains supply is disconnected before starting repairs
POSSIBLE FAULTS
1. Symptom Current and voltage readings show large fluctuations
Cause 1.1 Contact jaws or nozzle are worn or wrong size.
Action Replace contact jaws or nozzle.
Cause 1.2 Feed roller pressure is too low.
Action Increase pressure on feed rollers.
2. Symptom Wire feed is irregular
Cause 2.1 Feed roller pressure not correct.
Action Change the feed roller pressure.
Cause 2.2 Feed rollers wrong size.
Action Replace feed rollers.
Cause 2.3 Grooves in feed rollers are worn.
Action Replace feed rollers.
3. Symptom Welding cables overheating
Cause 3.1 Poor electrical connection.
Action Clean and tighten all electrical connections.
Cause 3.2 Cross--section of welding cables too small.
Action Use cables with a larger cross--section or use parallel cables.
ffa9d1ea
-- 7 6 --
Page 17
GB
8 ACCESSORIES
Manually operated slide 0154 465 xxx...............................................
Motor--driven slide 0334 333 xxx...................................................
Angular slide 0671 171 580........................................................
Contact equipment for twin wire 2x1.2 -- 2x2.0 Light duty 0333 852 881.................
Contact equipment for twin wire 2x2.0 -- 2x2.5--3.0 Heavy duty 0417 959 881............
Fine--wire straightener for single wire 0332 565 880...................................
Conversion kit A6 SFE1 to MIG/MAG welding 0334 299 890...........................
Conversion kit A6 SFE1/A6 SFE2 to Twin with fine--wire straightener (LD) 0334 291 888...
Conversion kit A6 SFE1/A6 SFE2 to Twin (HD) 0334 291 889..........................
Pilot lamp (D20) 0153 143 885......................................................
Adapter M6/M10 0147 333 001.....................................................
9 ORDERING OF SPARE PARTS
Spare parts are ordered through your nearest ESAB representative, see back cover.
When ordering spare parts, please state machine type and number as well as designation and spare part number as shown in the spare parts list on page 207.
This will simplify dispatch and ensure you get the right part.
ffa9d1ea
-- 7 7 --
Page 18
ESAB subsidiaries and representative offices
Europe
AUSTRIA
ESAB Ges.m.b.H
Vienna--Liesing
Tel: +43 1 888 25 11
Fax: +43 1 888 25 11 85
BELGIUM
S.A. ESAB N.V .
Brussels
Tel: +32 2 745 11 00
Fax: +32 2 745 11 28
THE CZECH REPUBLIC
ESAB VAMBERK s.r.o.
Prague
Tel: +420 2 819 40 885
Fax: +420 2 819 40 120
DENMARK
Aktieselskabet ESAB
Copenhagen--Valby
Tel:+4536300111
Fax:+4536304003
FINLAND
ESAB Oy
Helsinki
Tel: +358 9 547 761
Fax: +358 9 547 77 71
FRANCE
ESAB France S.A.
Cergy Pontoise
Tel:+33130755500
Fax:+33130755524
GERMANY
ESAB GmbH
Solingen
Tel: +49 212 298 0
Fax: +49 212 298 218
GREAT BRITAIN
ESAB Group (UK) Ltd
Waltham Cross
Tel: +44 1992 76 85 15
Fax: +44 1992 71 58 03
ESAB Automation Ltd
Andover
Tel: +44 1264 33 22 33
Fax: +44 1264 33 20 74
HUNGARY
ESAB Kft
Budapest
Tel:+3612044182
Fax:+3612044186
ITALY
ESAB Saldatura S.p.A.
Mesero (Mi)
Tel:+3902979681
Fax:+390297289181
THE NETHERLANDS
ESAB Nederland B.V.
Utrecht
Tel: +31 30 2485 377
Fax: +31 30 2485 260
NORWA Y
AS ESAB
Larvik
Tel:+4733121000
Fax:+4733115203
POLAND
ESAB Sp.zo.o.
Katowice
Tel: +48 32 351 11 00
Fax: +48 32 351 11 20
PORTUGAL
ESAB Lda
Lisbon
Tel: +351 8 310 960
Fax: +351 1 859 1277
SLOVAKIA
ESAB Slovakia s.r.o.
Bratislava
Tel:+421744882426
Fax:+421744888741
SPAIN
ESAB Ibérica S.A.
Alcalá de Henares (MADRID)
Tel: +34 91 878 3600
Fax: +34 91 802 3461
SWEDEN
ESAB Sverige AB
Gothenburg
Tel:+4631509500
Fax:+4631509222
ESAB International AB
Gothenburg
Tel:+4631509000
Fax:+4631509360
SWITZERLAND
ESAB AG
Dietikon
Tel: +41 1 741 25 25
Fax: +41 1 740 30 55
North and South America
ARGENTINA
CONARCO
Buenos Aires
Tel: +54 11 4 753 4039
Fax: +54 11 4 753 6313
BRAZIL
ESAB S.A.
Contagem--MG
Tel: +55 31 2191 4333
Fax: +55 31 2191 4440
CANADA
ESAB Group Canada Inc.
Missisauga, Ontario
Tel: +1 905 670 02 20
Fax: +1 905 670 48 79
MEXICO
ESAB Mexico S.A.
Monterrey
Tel: +52 8 350 5959
Fax: +52 8 350 7554
USA
ESAB Welding & Cutting Products
Florence, SC
Tel: +1 843 669 44 11
Fax: +1 843 664 57 48
Asia/Pacific
CHINA
Shanghai ESAB A/P
Shanghai
Tel: +86 21 5308 9922
Fax: +86 21 6566 6622
INDIA
ESAB India Ltd
Calcutta
Tel: +91 33 478 45 17
Fax: +91 33 468 18 80
INDONESIA
P.T. ESABindo Pratama
Jakarta
Tel: +62 21 460 0188
Fax: +62 21 461 2929
JAPAN
ESAB Japan
Tokyo
Tel: +81 3 5296 7371
Fax: +81 3 5296 8080
MALAYSIA
ESAB (Malaysia) Snd Bhd
Shah Alam Selangor
Tel: +60 3 5511 3615
Fax: +60 3 5512 3552
SINGAPORE
ESAB Asia/Pacific Pte Ltd
Singapore
Tel: +65 6861 43 22
Fax: +65 6861 31 95
SOUTH KOREA
ESAB SeAH Corporation
Kyungnam
Tel: +82 55 269 8170
Fax: +82 55 289 8864
UNITED ARAB EMIRATES
ESAB Middle East FZE
Dubai
Tel: +971 4 887 21 11
Fax: +971 4 887 22 63
Representative offices
BULGARIA
ESAB Representative Office
Sofia
Tel/Fax: +359 2 974 42 88
EGYPT
ESAB Egypt
Dokki--Cairo
Tel: +20 2 390 96 69
Fax: +20 2 393 32 13
ROMANIA
ESAB Representative Office
Bucharest
Tel/Fax: +40 1 322 36 74
RUSSIA--CIS
ESAB Representative Office
Moscow
Tel:+70959379820
Fax: +7 095 937 95 80
ESAB Representative Office
St Petersburg
Tel:+78123254362
Fax: +7 812 325 66 85
Distributors
For addresses and phone
numbers to our distributors in
other countries, please visit our
home page
www.esab.com
ESAB AB
SE--695 81 LAXÅ
SWEDEN
Phone +46 584 81 000
www.esab.com
041227
 Loading...