

Page 1
Always Moving Forward
®
Operating Manual
Please Read Before Operating Unit
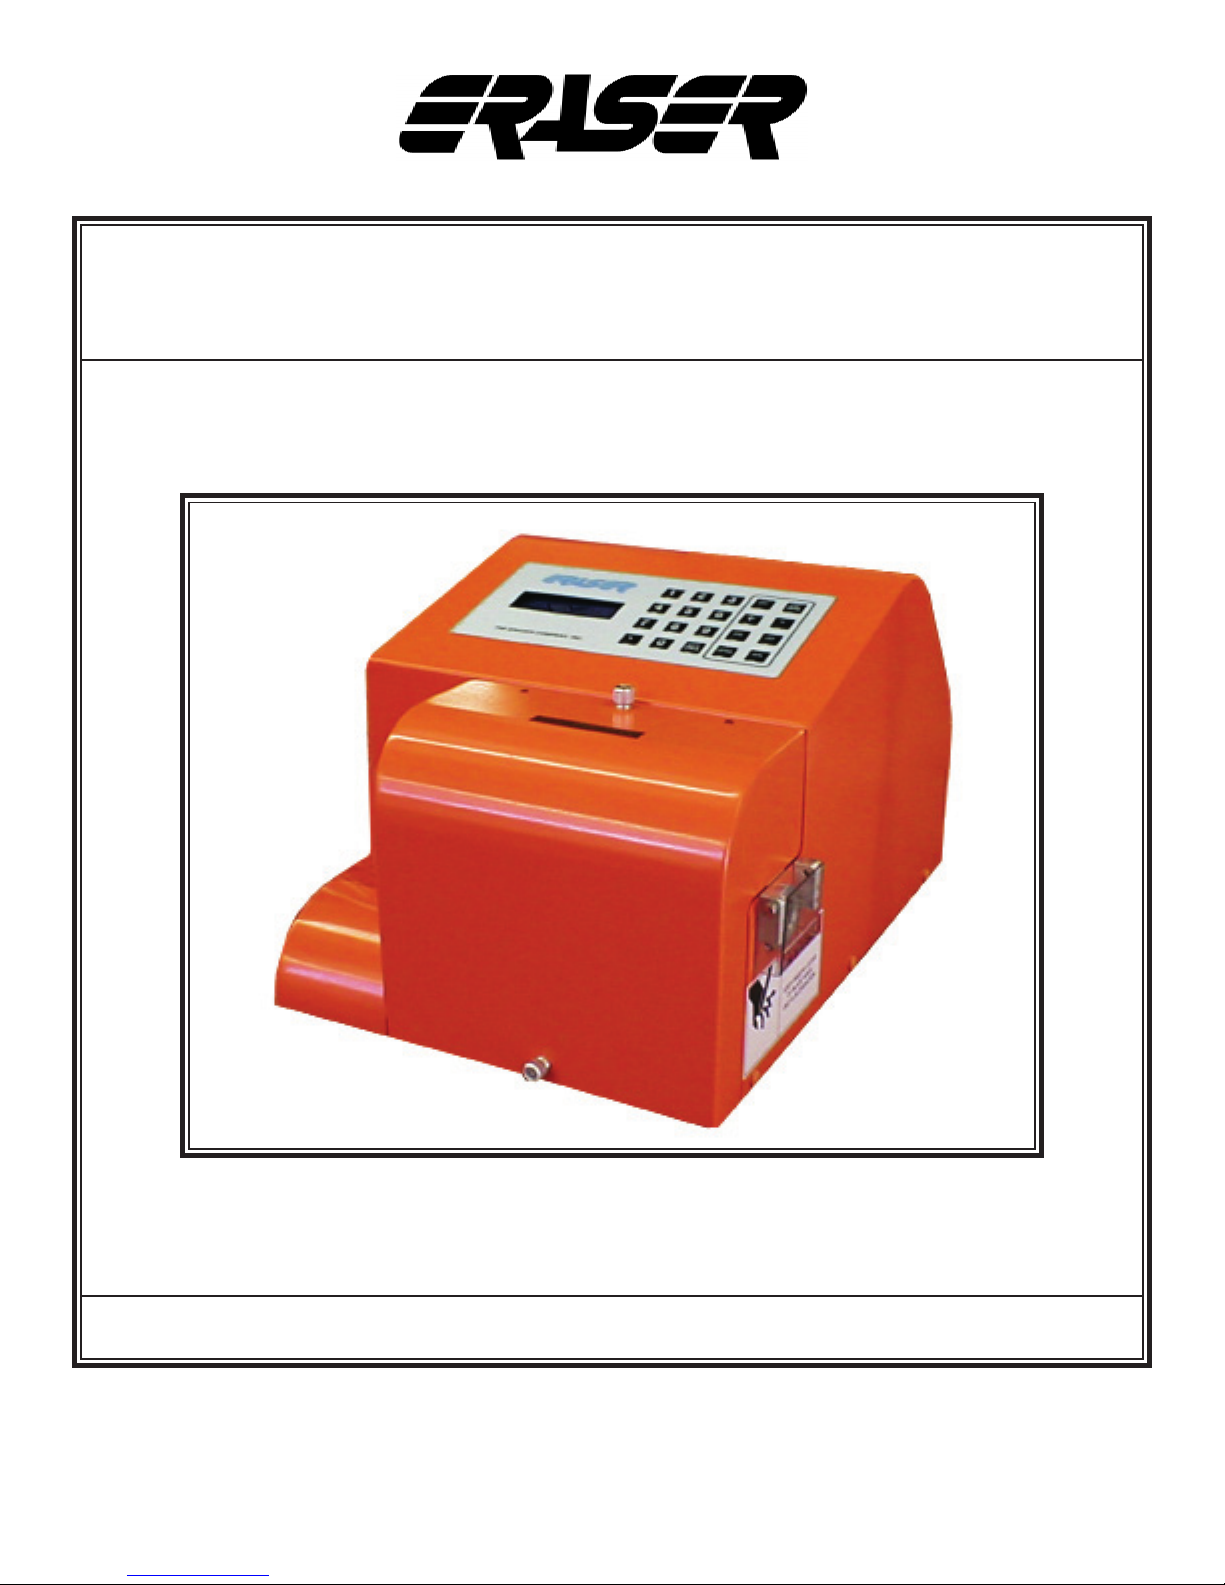
Model WC601D Automatic Tubing Cutter
The Eraser Company, Inc.
PO Box 4961/ Oliva Drive
Syracuse, NY 13221, USA
Service and All Spare Parts Available
Phone: (315) 454-3237
Fax: (315) 454-3090
Website: www.eraser.com
E-mail: [email protected]
Page 2
Always Moving Forward®
SPECIFICATIONS
Minimum material size ............... ½” (12.7 mm) tubing
Maximum material size ......... 1 1/8” (28.5 mm) tubing
Maximum number of pieces ......... 99,999 (per batch)
Minimum cut length .............. 0.10” (0.25 cm) or less;
material dependent
Maximum cut length ................ 99,999” or 99,999 cm
Length Resolution............................ 0.01” or 0.01 cm
Dimensions .......................12 1/8”W x 16 ¾”D x 10”H
Weight ............................................ 45 LBS (20.5 kg)
Tolerances
Repeatability ........+/- 0.005” (0.13 mm) to 5% of total
length; dependent on material and dereeling system
Squareness of cut........ 0° +/- 2°; material dependent
Performance
Cut Rates.......................10 selectable cut rates (0-9)
Feed Rates ..................10 selectable feed rates (0-9)
p 2
WC601D AUTOMATIC
TUBING CUTTER
Power & Usage
Voltage; Frequency..................................120V; 60Hz
Consumption ............................................. 150 Watts
Usage rating ............................................ Continuous
Operating Environment
Operating temperature .......... 50° - 90°F (10° - 32°C)
Airow ........ Unobstructed, well-ventilated workspace
ORDERING INFORMATION
AR7151 (WC601D):
Automatic Large Tubing Cutter, 120V
Included Parts
WC601D ships with the following parts/tools:
• (1) 5/64” Allen wrench (for the 3 bushing set screws)
(item #TG3028)
• (1) 3/32” Allen wrench (for the 2 blade stop screws
(item #TG3790)
• (1) 5/32” Allen wrench (for the 2 blade retention screws)
(item #TG0026)
• (2) PR1029 Feed belts (installed)
• (1) IR1296 Cut blade (installed)
• (1) Power cord
Programming
Batching...................up to 99 programmable batches
Kits.......................................................... up to 10 kits
(depending upon available memory)
WC601D Linear Speeds
Feedrate #inches/
sec
cm/sec
0 4.8 12.1
1 9.5 24.2
2 11.9 30.2
3 16.7 42.3
4 19.1 48.4
5 21.4 54.4
6 26.2 66.5
7 28.6 72.6
8 33.3 84.6
9 35.7 90.7
Replacement Parts
IR1296 .......................................................... Cutting Blade
(1 required; 1 supplied)
PR1029....................................................Timing Feed Belt
(2 required; 2 supplied)
PR3146.............................................. Blade Return Spring
(1 required; 1 supplied)
PG1032 ......................................... O Ring, Blade Cushion
(1 required; 1 supplied)
IR0977 ......................................... Set of Custom Bushings
(sold separately)
PR0655..................... Fuse, for 120V IEC connection
(1 required; 1 supplied w/AR7151)
PR2727.................................................. Power cord, 120V
(1 required; 1 supplied w/AR7151)
PR1026...............................Flat Belt for Rotary Head
(Please call us for pricing and availability of replacement parts.)
Optional Parts/Accessories
IR1390 ...................... Optional Carbide Cutting Blade
AR0010(DE100) ...........................Turntable Dereeler
AR3801(DE400) ................ Bench Mounted Dereeler
AR0170(DE700) .................. Compensating Dereeler
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 3
MODEL WC601D AUTOMATIC TUBING CUTTER
p 3
IMPORTANT SAFETY INSTRUCTIONS
IMPORTANT! DO NOT OPERATE MACHINE
UNTIL YOU HAVE READ THOROUGHLY, AND
UNDERSTAND COMPLETELY, ALL PRECAUTIONS,
INSTRUCTIONS AND INFORMATION ON THESE
PAGES. THIS MANUAL CONTAINS IMPORTANT
SAFETY AND OPERATING INSTRUCTIONS. IT
SHOULD BE RETAINED WITH THE MACHINE FOR
FUTURE REFERENCE.
SAFETY PRECAUTIONS - MECHANICAL
! DO NOT OPERATE UNIT WITHOUT GUARDS IN
PLACE OR WITH DAMAGED GUARDS.
! DO NOT DEFEAT ANY OF THE SAFETY FEATURES.
! DO NOT PLACE FINGERS OR APPENDAGES
NEAR MOVING PARTS OR IN OR NEAR
OPENINGS IN GUARDS.
SAFETY PRECAUTIONS - ELECTRICAL
! ALWAYS UNPLUG UNIT FROM POWER SUPPLY
PRIOR TO ANY MAINTENANCE.
! DO NOT RUN UNIT WITH INCORRECT LINE VOLTAGE.
! NEVER RUN MACHINE WITH DAMAGED OR
WORN POWER CORD.
! NEVER MODIFY THE PLUG PROVIDED. IF IT
WILL NOT FIT INTO THE OUTLET, HAVE THE
PROPER OUTLET INSTALLED BY A QUALIFIED
ELECTRICIAN.
GROUNDING INSTRUCTIONS Grounding provides
a common return path for electric current to reduce
the risk of electric shock. This machine is supplied
with an electric cord with an equipment-grounding
conductor and a grounding plug. The plug must
be plugged into a matching outlet that is properly
installed and grounded in accordance with all local
codes and ordinances.
Improper connection of the equipment-grounding
conductor can result in a risk of electric shock.
Check with a licensed electrician if in doubt as to
whether the machine is properly grounded.
SAFETY FIRST - USE BEST PRACTICES
ALWAYS USE SAFETY GLASSES Everyday
eyeglasses only have impact resistant lenses; they
are NOT safety glasses. Also use face or dust mask
if cutting operation is dusty.
REMOVE ADJUSTING KEYS AND WRENCHES
Form a habit of checking to see that keys and
adjusting wrenches are removed from machine
before turning it on.
KEEP WORK AREA CLEAN Cluttered areas and
benches invite accidents. Always leave at least 12”
(305 mm) of space around all sides and top of unit.
DON’T USE IN DANGEROUS ENVIRONMENTS
Do not use or locate machine in high-humidity
environments, or expose to rain. Keep work areas
well lighted.
WEAR PROPER APPAREL Do not wear loose
clothing, such as gloves, neckties, rings, bracelets,
necklaces or any other clothing or jewelry that might
get caught in moving parts. This is not an all-inclusive
list. Wear protective hair covering to contain long hair.
Non-slip footwear is recommended.
DON’T OVERREACH Maintain proper footing and
balance at all times.
MAINTAIN BLADES WITH CARE Keep blades
sharp and clean for optimal performance. Follow
instructions for lubricating and changing blades and
all accessories.
DISCONNECT MACHINE FROM POWER SUPPLY
Unplug the unit before servicing and when changing
accessories.
DO NOT EXCEED THE UNIT’S MAXIMUM
MATERIAL SPECIFICATIONS Eraser’s warranty
will be null and void if machine has been used in any
manner that is contrary to these instructions.
CHECK FOR DAMAGED PARTS Before continued
use of the machine, the guard and all moving parts
should be carefully inspected to ensure that nothing
is damaged.
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 4
MODEL WC601D AUTOMATIC TUBING CUTTER
p 4
ENSURE PROPER ALIGNMENT OF MOVING
PARTS Check for any binding of moving parts,
breakage of parts, and any other condition(s) that
may affect operation. Any damaged part(s) should
be properly repaired or replaced prior to any
continued use of the machine.
ONLY ALLOW TRAINED AND QUALIFIED
PERSONNEL TO OPERATE UNIT Always keep
these instructions within reach of the machine.
USE RECOMMENDED ACCESSORIES ONLY
Consult this operating manual for recommended
accessories. Use only parts supplied by The Eraser
Company, Inc. Use of improper accessories will void
Eraser’s warranty and may increase risk of injury.
ALL REPAIRS SHOULD BE PERFORMED BY AN
ERASER COMPANY REPRESENTATIVE ONLY
Unauthorized disassembly of machines will void
Eraser’s warranty.
a sales representative for more details.
The WC601D may also be used with a tensioning
dereeler or an automatic pre-feed system. Use
of the Model DE700 Compensating Dereeler
is recommended. This device will improve the
accuracy and/or productivity of the WC601D. If
using the DE700 (or any other dereeling system),
place the dereeler to the left side of the WC601D,
approximately 24” (for elastic materials the distance
may be reduced) from the entrance bushing in a
straight line and align the exit pulley of the dereeler
with the entrance bushing of the WC601D. If using
the DE700, refer to the operating manual for further
set up details.
First, remove the unit’s front cover/guard by
loosening the (2) thumb screws located on the front
and top of the front cover. Referring to the drawing
on page 16, locate the blade stop adjusting screw
on the cutting head.
WHEN USING MACHINERY, ALL SAFETY
PRECAUTIONS – INCLUDING, BUT NOT LIMITED TO,
THOSE LISTED ABOVE - SHOULD BE FOLLOWED
TO REDUCE THE RISKS OF FIRE, ELECTRIC SHOCK,
AND PERSONAL INJURY, AND DEATH.
IMPORTANT: NO LIABILITY WILL BE INCURRED
BY THE ERASER CO. FOR INJURY, DEATH, OR
PROPERTY DAMAGE CAUSED BY A PRODUCT
WHICH HAS BEEN SET UP, OPERATED, AND/OR
INSTALLED CONTRARY TO ERASER’S WRITTEN
OPERATING MANUAL, OR WHICH HAS BEEN
SUBJECTED TO MISUSE, NEGLIGENCE, OR
ACCIDENT, OR WHICH HAS BEEN REPAIRED
OR ALTERED BY ANYONE OTHER THAN THE
ERASER COMPANY, OR WHICH HAS BEEN
USED IN A MANNER OR FOR A PURPOSE FOR
WHICH THE PRODUCT WAS NOT DESIGNED.
SET-UP: Check your shipment to be sure all items
listed under the parts section are in the box. If
anything is missing, please let us know immediately.
Prior to shipment, the blade stop adjusting screw
has been set to lock the blade holder in the open
position, to secure it during transport. Prior to
bushing installation (see below) loosen the locking
set screw (which secures the blade stop screw),
then back the blade stop screw away from the blade
holder mechanism.
BUSHING INSTALLATION: (Refer to the drawing on page 15)
The WC601D requires one (1) set of custom
bushings. A bushing set consists of one (1) of each
of the following: the entrance bushing (7/8” long w/
hub); the head (middle) bushing (2 5/8” long); & the
exit bushing (1 3/8” long), for a total of 3 bushings.
If different sizes of material are going to be cut,
additional bushing sets may be ordered.
First install the head bushing. Lift the clear guard on
the right side of the unit and insert the ID-chamfered
end of the head bushing into the hole under the
clear guard. Slide the head bushing completely past
the blade on the cutting head.
Place the model WC601D on a sturdy workbench.
A material collection bin can be placed on the right
side of the unit, beneath the clear guard.
NOTE: It is possible for the WC601D to be controlled
by an external device or process, by using the DB9
connector located on the rear panel of the unit. Contact
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Manually actuate the blade holder (see Set-up,
above) and slide the head bushing back toward the
blade until the clearance between the bushing &
the blade is approximately 1/32”. Tighten the head
bushing in place, then lift the clear guard and insert
the exit bushing until the bushing is approximately
1/32” from the opposite side of the blade from the
Page 5
MODEL WC601D AUTOMATIC TUBING CUTTER
p 5
head bushing and tighten with the set screw. Make
certain that the blade moves freely by manually
actuating it.
Reposition & retighten the head bushing (keeping
it as close as possible to the blade without
interference) if it interferes with the blade path. This
will provide the squarest possible cut and allow
small pieces to be run. Also, head bushings that are
not close to the blade may cause material to jam,
when cutting short pieces.
Lastly, install the entrance bushing into the bushing
block to the left of the feed belts, until the hub of the
bushing is ush with the bushing block. Tighten the
head bushing and replace front cover/guard.
OPERATION:
Insert the power cord into the machine’s IEC
connector, and plug the unit into a 120V 60Hz mains
supply.
! CAUTION: Prior to connection, ensure that the
power supply is properly grounded.
Turn the WC601D on using the I/O switch on
the back side of the unit (located within the IEC
connection housing). To open the front cover,
unscrew the top and front thumb screws. Most
tubing can be fed through the feed belts by using
the manual control keys located on the keypad (the
<JOG>, <+> and <-> keys). The <JOG> and <+>
keys jogs the material through the machine and the
<-> key reverses this movement. Insert the material
through the entrance bushing to the feed belts and
press the <JOG> key or the <+> key. Press the
<CUT> key when the material has been completely
fed through the exit bushing to eliminate the excess
length on the rst piece.
If the material won’t feed through the machine
correctly, feed the material into the entrance bushing
and open the belt feed by turning the adjusting
knob counterclockwise. Manually feed the material
between the belts and through the head and exit
bushings. Clockwise rotation of the belt feed tension
knob will result in more tension. Counterclockwise
rotation will result in less tension. If the material is
slippery, more tension may be applied to the belt
feed by turning the tension adjusting knob clockwise.
Apply only enough tension to transport the material
consistently - do not over-tighten feed belts. Over
tightening the feed belts causes excessive drag in
the bushings and accelerates feed belt wear.
The feed belts should be adjusted by tightening them
just until the material can no longer be pulled between
them by hand. More belt pressure may be added if cut
lengths are inconsistent. Once material has been fed
through the bushings and belt tension is set, tighten
the lock nut (located underneath the belt feed tension
adjusting knob), then replace the front cover.
NOTE: Using the <JOG> key places the controller in
Manual mode. When in Manual mode, the MANUAL
PROCESS screen displays:
MANUAL PROCESS
LENGTH: 0.0
ABORT –ESC
The length indication increments or decrements with
regard to the motion induced by the <+>,
<-> or <JOG> keys. The indicator resets to zero
when the cut key is pressed. Press the <ESC/
PAUSE> key to return to the BATCH SELECT
screen. The unit now is ready for programming
START UP:
Turn the WC601D on using the I/O switch on the
rear face of the unit. When the unit is turned on, the
splash screen will display briey:
THE ERASER COMPANY
WC601D[rmwarerevisiondate]
The main BATCH SELECT screen is displayed next:
DO ONE OF THESE: 0
0 FOR NO BATCH SAVE
ENTER . FOR KIT
NEXT NEW BATCH #1
NOTE: Do not turn the unit on and off repeatedly
without waiting 5 seconds.
With the cover off the unit, open the feed belts
enough to accommodate the material being fed.
Material can now be fed through the feed belts
semi-automatically by rst pressing the <JOG>,
<+> and <-> keys. The <+> key jogs the material
forward (toward the cutter) and the <-> key reverses
this movement. Press the <CUT> key when the
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 6
MODEL WC601D AUTOMATIC TUBING CUTTER
p 6
material has been fed past the blade by at least ¼”.
This will eliminate the excess material length on the
rst piece of a programmed batch. When using the
<JOG> key, the controller is in manual mode, and
the MANUAL PROCESS screen displays:
MANUAL PROCESS
LENGTH: 0.0
ABORT –ESC
The length indication increments or decrements
with regard to the motion induced by the <+>, <->
or <JOG> keys. The length indicator resets to zero
after the <CUT> key is pressed. Press the <ESC/
PAUSE> key to return to the BATCH SELECT
screen. The unit now is ready for programming.
PROGRAMMING:
EXPLANATION OF BATCH PROGRAMMING
Referring to the BATCH SELECT screen above, the
number on the rst line will be the last batch run, or
in this case, 0, since no processing has occurred
after power-up. A “batch” is a program, or a set of
parameters for a quantity of a specied length to be
cut (i.e. the unit of measure, the cut length, length
adjustment [compensation], quantity, cut rate and
feed rate). The number on the last line is the next
available batch that has not yet had parameters
stored (i.e. it is a clean memory location and is
the location of the next batch to be programmed).
The system requires that batches be created in
sequence, so numbers higher than the number on
the last line will not be accepted. As batches are
created, the number on the last line of the BATCH
SELECT screen will increase, until the maximum of
99 batches is reached. Parameters entered while
using batch 0 are never stored after the unit is
turned off (the “0” batch is a “scratch pad” memory
location). Parameters for all other batches (1-99)
are stored, so the next time that particular batch
is called, those parameters will be presented as
entered.
PROGRAMMING BATCHES:
Press the <ENTER> key to select the Default Batch
(0), or type in either an existing stored batch (to edit
or review), or input a new batch number as indicated
on the last line of the main menu. (“NEXT NEW
BATCH #”). Press the <ENTER> key. Values will be
stored for the next time that batch is entered (except
batch 0). All batches that have parameters stored can
be edited, reviewed or run by entering the desired
batch number at the “DO ONE OF THESE” prompt.
CREATING A NEW BATCH:
Enter the number on the last line of the BATCH
SELECT screen, using the above example, Batch #
1, then press the <ENTER> key. The BATCH EDIT
screen will appear:
UNITS in #1
CUT LENGTH .0
LENGTH ADJUST 0
QUANTITY 0
The current batch number is shown beside the # at
the top right. The cursor will be ashing just before
the default input of “in” (inches), indicating that the
eld is currently editable. The line being edited will
display a blinking cursor.
“UNITS” parameter: Press the <ENTER> key to
accept the default of inches, or press the <+> or <->
key to toggle to “cm”, for centimeters, then press the
<ENTER> key to store the selected unit of measure.
NOTE: Each time the <ENTER> key is pressed, the
cursor advances to the next parameter.
“CUT LENGTH” parameter: Enter a value for the
length parameter. If the <ENTER> key is pressed
accidentally before a value is entered, the unit will
sound a long beep, to prompt the entry of a number
greater than zero (CUT LENGTH and QUANTITY
elds). If a mistake is made prior to pressing the
<ENTER> key, press the <BACKSPACE> key to
back space over the entry. If the <ENTER> key
has been pressed after an incorrect entry, a long
beep is heard and an error code is displayed (see
“DATA ENTRY ERROR CODES & SOUNDS ”
section below). The cursor then returns to the eld
where the entry error was made. The CUT LENGTH
parameter requires a value between .01 and 99,999
to be entered. The limitation here is that the value
can be a maximum of 6 characters – including
the decimal point - if a decimal point is used. The
maximum decimal value is two places (hundredths
of a unit). For example, 123.45 and 1234.5 are
permissible but the value 1234.56 isn’t allowed. If
a decimal is not used, the maximum number of
characters is 5 for this eld.
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 7
MODEL WC601D AUTOMATIC TUBING CUTTER
p 7
NOTE: Due to variations in materials, pre-feed
systems, belt feed tension or feed rate, actual
cut length may vary from the inputted length by a
proportional amount.
After running a batch or manual single piece (see
BATCH START screen instructions below), it is
recommended to measure the length of the cut
piece(s). If the cut length(s) are consistent with each
other, the machine requires no further adjustment to
either the pre-feed system (if applicable), belt feed
tension or feed rate.
“LENGTH ADJUST” parameter: The WC601D
incorporates a length compensation feature to
provide an easy adjustment in these cases. The
length can be compensated in increments of 1%,
from -10% to +10% of the value entered into the
CUT LENGTH eld. The length compensation
display will show (-) for a negative value. Example:
If 10” is entered as the desired length, but the
actual average cut piece measures 9.8”, a length
compensation of +2% will increase the cut length by
.200 to the desired 10” The <+> or <-> keys may
be used to add or decrease length compensation
value. NOTE: Often it will not be known if length
compensation is needed until after a trial run
is completed. When programming a batch, it is
recommended to leave the LENGTH ADJUST
eld at 0 and edit this eld later if necessary to
incorporate length compensation. Once a value has
been entered, or if the default of 0 is to be used,
press the <ENTER> key.
“QUANTITY” parameter: Enter a quantity from 1 to
99,999. Only integers (no decimals) will be accepted
for this eld.
After the quantity is entered, the CUT RATE screen appears:
CUT RATE 3 #1
-CUT SPEED 70%
-POST DELAY 1250
CUT TIME 1.0
The Cut Rate in the rate at which the rotary blade
cuts material. The default cut rate is 3, as shown
above. The Cut Rate can be changed at this point
by entering a number (from a minimum rate of 0
through a maximum rate of 9) or by pressing the
<+> or <-> keys. As the value is changed, the CUT
SPEED and POST DELAY values (not editable)
are updated to show what values are active for the
selected cut rate. Input the desired cut rate and
press the <ENTER> key. Then enter the desired
Cut Time in seconds. This is the amount of time
that the rotary head is powered during the cut cycle.
The default cut time 1.0 second for all cut rates. 1
second is the recommended minimum cut time.
After the cut rate is entered, the FEED RATE screen
now appears:
FEED RATE 3 #1
-MAX SPEED 8.0
-MAX ACCEL 20.0
-MAX DECEL 40.0
The Feed Rate is the rate at which material will
travel through the feed belts prior to the cut cycle.
The default feed rate is 3, as shown above. As with
the CUT RATE screen, the FEED RATE can be
changed at this point by entering a number (from a
minimum rate of 0 through a maximum rate of 9) or
by pressing the <+> or <-> keys. Input the desired
feed rate and press the <ENTER> or <RUN> key.
NOTES:
• The slower the feed rate, the more accurate in
length the cut pieces will be. It is recommended
to start with a middle-range feed rate (3 or 4) and
check results, then adjust the feed rate up or down
as needed.
• For the FEED RATE screen, the MAX SPEED, MAX
ACCEL & MAX DECEL parameters are not editable.
DATA ENTRY ERROR CODES & SOUNDS:
If an incorrect key is pressed for a given parameter
input (e.g. a number key is pressed at the prompt for
a unit of measure or for the length correction factor),
a long beep will sound that is distinctly longer than
the short beep heard after each key press. Also, if
the value entered is out of range or isn’t acceptable
as an input for that parameter (e.g. entering more
than 99,999 as a length, or using more than 2
decimal places, etc.) a letter appears in the lower
right corner of the display (‘R’ as highlighted in the
example below) indicating the error:
UNITS in #1
CUT LENGTH .0
LENGTH ADJUST 0
QUANTITY 0 R
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 8
MODEL WC601D AUTOMATIC TUBING CUTTER
p 8
INPUT ERROR DIAGNOSTIC LEGEND
R - Data out of range.
D - An extra decimal point.
W - A decimal only was entered as an input (no
numbers)
N - Nothing to delete. Back Space key pressed too
many times.
L - Length out of range.
F - Too many decimal places.
KEYPAD LEGEND:
<ENTER> key: Advances to next parameter or
screen. When editing an existing batch parameter,
an <ENTER> key press is necessary to re-write a
new value for a parameter into memory.
<RUN> key: Advances to the next screen/menu
without over writing existing values.
<ESC/PAUSE> key: Returns to the previous screen.
Pauses batch processing.
Once the feed rate is entered, press the <ENTER>
or <RUN> key to advance to the BATCH START
screen:
JOG - JOG
CUT - CUT
MAIN MENU - ENTER
START – RUN
This menu allows several options:
• to run a test piece (<JOG> & <CUT> keys);
• to cut a piece (<CUT> key);
• to enter the newly created batch parameters into
memory without running the batch (<ENTER> key);
• or to simply run the batch as programmed (<RUN> key).
<JOG> key: If the operator chooses to run some
test pieces before commencing the batch, press
the <JOG> key to display the MANUAL PROCESS
screen:
MANUAL PROCESS
LENGTH: 0.0
ABORT –ESC
NOTE: This screen looks like the MANUAL
PROCESS screen (as described under Start up,
above) but has a subtle difference. When the
<JOG> or <+> keys are pressed, material will feed
the distance that is programmed in the cut length
parameter of the current batch. For example, if 5.0”
was entered as a cut length, a <JOG> or <+> key
press would advance 5” of material through the
machine and 5.0 would be displayed for a length.
Another <JOG> or <+> key press would again
advance 5 inches of material through the machine
and 10.0 would be displayed as the total length run in
this mode. Following this example, pressing the <->
key next would reverse the material by 5 inches, and
5.0 would again be displayed as the length, giving
you the total amount of material remaining to be cut.
<CUT> key: The cut mechanism activates and the
length is reset to zero.
<RUN> key (START option): The BATCH RUN
screen is displayed:
PIECES XXXX #1
PIECES LEFT XXXX
ESC TO STOP/BREAK
RUN TO CONTINUE
The rst line indicates the quantity parameter and the
current batch number and the second line displays
a running count of the pieces left to process. The
PIECES LEFT count is decremented after each
piece is cut. Pressing the <ESC/PAUSE> key during
batch processing stops the machine and displays the
BATCH ESCAPE/GUARD REPLACE screen:
JOG - JOG
CUT - CUT
ABORT - ESC
CONTINUE - RUN
To resume the batch, press the <RUN> key, or press
the <JOG> or <+> key to advance material, or the
<-> to reverse material.
Press the <CUT> key to cut material.
Press the <ESC/PAUSE> key again to abort
the batch. This will bring the use to the BATCH
COMPLETION screen, as shown below. The
number of pieces remaining to be cut (unprocessed
portion of the batch) is displayed in the PIECES
LEFT parameter.
When a batch is successfully completed, the BATCH
COMPLETION screen appears:
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 9
MODEL WC601D AUTOMATIC TUBING CUTTER
p 9
RUN COMPLETE #1
PIECES LEFT 0
PUSH ANY KEY
This screen indicates a successful completion of a
batch and the batch number completed. Any key
press brings the main batch select menu back to the
BATCH SELECT screen.
RUNNING AN EXISTING BATCH:
Once a batch has been created and run, it may
be started with a little as three key presses: After
running a batch, it remains the default batch number
until another batch is run or edited. To run the batch
again, press any key at the BATCH COMPLETION
screen, then press the <RUN> key twice.
Alternatively, a different batch may be selected
and run by pressing any key from the BATCH
COMPLETION screen, then entering the batch
number (i.e. selecting a batch number that already
exists in memory) at the “DO ONE OF THESE”
prompt, then pressing the <RUN> key twice.
In addition to manually pausing a batch, removing
the guard will also interrupt processing. If the guard
is removed during a running batch, or when pressing
<RUN> to begin a batch, the message:
piece). The WC601D will then process all pieces in
batch number 4, then batch 5, then batch 6. However,
batches do not need to be programmed in sequential
(batch-numbered) order within a kit.
First, a kit is programmed by assigning batches to it,
and then the quantity of kits to be processed is entered
at the end of the Kit programming. Kit quantities are
not saved or stored within kit programming.
Kit programming is initiated by entering pressing the
< . > (decimal) key at the default BATCH SELECT screen.
After the < . > (decimal) key is pressed, the KIT
SELECT screen appears:
SELECT KIT 1
NEXT NEW KIT #2
At this point, the operator has 3 options:
1) The operator can dene a new kit.
2) The operator selects an existing kit number, if
previously dened. To run a dened kit, enter the
kit number, then press the <RUN> key twice to go
directly to the KIT QUANTITY screen (shown below,
just before the Automode Kit Operation section).
3) The operator can return to the BATCH SELECT
screen by pressing the <ESC/PAUSE> key.
GUARD OPEN!
appears on the screen. When the guard is removed,
the machine will stop immediately, and will not
run until the guard is replaced. When the guard is
replaced, the BATCH ESCAPE/GUARD REPLACE
screen appears:
JOG - JOG
CUT - CUT
ABORT - ESC
CONTINUE – RUN
For descriptions of these functions, refer to the
instruction under the BATCH ESCAPE/GUARD
OPEN screen above.
KITTING FEATURE:
The WC601D also has a Kitting feature. This allows
a collection (or set) of batches to be run sequentially.
A Kit can be dened, for example, to be Batches 4
(one 6.0” piece), 5 (three 8.0” pieces) and 6 (one 2.0”
Since we’ll be describing kit programming, we’ll
follow option #1 above. Press the <ENTER> key at
the KIT SELECT screen above, using the default
of ‘1’ as the kit to be programmed. The KIT EDIT
screen displays:
INDEX #0 F KIT#1
SELECT BATCH: 0 A
LENGTH .0
QUANTITY 0
INDEX is the “place holder” within the kit that stores
the batch. The rst batch in any kit is stored at Index
#0, the second batch position in the kit is Index #1,
and so forth. Therefore, Batch position = [Index #]
+1. After inputting ‘1’ at the KIT SELECT screen,
the cursor is at the ‘SELECT BATCH:’ parameter of
the KIT EDIT screen (above). The Position Indicator
(see table below for Indicator denitions) displays
an “F”, meaning that this is the “rst” batch in this
kit. In addition, the Allowable Action Indicator (see
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 10
MODEL WC601D AUTOMATIC TUBING CUTTER
p 10
table below for Indicator denitions) displays an “A”,
meaning that a batch may be “added”.
POSITION INDICATOR – Located between INDEX
# and KIT #, on the rst (top) line.
SymbolDenition
F - First batch in kit (index #0).
M - Middle batch.
L - Last batch (last index in kit, can be deleted/changed).
N - New index position (this status is temporary until
this index/batch is saved).
ALLOWABLE ACTION INDICATOR – Located after
Batch number, on the second line.
SymbolDenition
E - Edit - can change batch # at current index.
D - Delete - remove or change batch from current
index (only possible for the last index in the kit),
also implies an edit if it is necessary.
A - Add - add batch and index location to kit (batch
not yet selected for current INDEX).
To continue with the example outlined above, Batch
4 will be the rst batch to be run in this kit so it will
be entered at index 0. The operator presses the <4>
key, then the <ENTER> key, to enter Batch #4 as
Index #0 of the kit. The KIT EDIT screen displays:
INDEX #0 F KIT#1
SELECT BATCH: 4 D
LENGTH 6.0
QUANTITY 1
The batch number, length and quantity are displayed
for the entered batch (in this example, Batch 4) and
the Allowable Action Indicator (see table above)
changes to a “D”, meaning that this batch number
can be “deleted” from the kit. When the operator is
satised he/she has chosen the correct batch, press
the <+> or <ENTER> key to move to the next index,
and to enter the next batch in the kit’s sequence.
The KIT EDIT screen displays:
INDEX #1 N KIT#1
SELECT BATCH: 0 A
LENGTH .0
QUANTITY 0
position) and the Allowable Action Indicator displays
an “A”, meaning that a batch number can be “added”
to this location. The operator then presses the <5>
key, then the <ENTER> key to place Batch 5 into the
second sequence in this kit. The KIT EDIT screen
displays:
INDEX #1 L KIT#1
SELECT BATCH: 5 D
LENGTH 8.0
QUANTITY 3
The Position Indicator now displays an “L” (the “last”
batch in this kit so far) and the Allowable Action
Indicator displays a “D”, meaning that this batch
can be “deleted” from the kit. Only the last batch
in a kit may be deleted. When the “D” is displayed,
the operator can delete the batch from the kit by
pressing the <CUT> key. When the operator is
satised he/she has chosen the correct batch, press
the <+> or <ENTER> key to move to the next index,
and to enter the next batch in the kit’s sequence.
The KIT EDIT screen displays:
INDEX #2 N KIT#1
SELECT BATCH: 0 A
LENGTH .0
QUANTITY 0
The Position Indicator displays an “N” (indicating
a “new” index position) and the Allowable Action
Indicator displays an “A”, meaning that a batch can
be “added” to this location. To enter the last batch in
this example kit, the operator presses the <6> key
and then the <ENTER> key. The KIT EDIT screen
displays:
INDEX #2 L KIT#1
SELECT BATCH: 6 D
LENGTH 2.0
QUANTITY 1
With this last batch, the example kit is completely
dened. When the kit is fully dened, the operator
presses the <RUN> key to run the kit, or the <ESC/
PAUSE> key to go back to the KIT SELECT screen. A
<RUN> key press displays the KIT QUANTITY screen:
The second location is numbered INDEX #1 (the
counting for indexes starts at zero), the Position
Indicator displays an “N” (indicating a “new” index
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
QUANTITY: 0 KIT#1
ENTER 0 FOR MANUAL
OR # FOR AUTOMODE
Page 11
MODEL WC601D AUTOMATIC TUBING CUTTER
p 11
AUTOMODE KIT OPERATION:
(PROCESSING A KIT AT A SPECIFIC QUANTITY)
Kit quantities must be entered each time a kit is
called up and processed, they are not stored in
the kit’s program or from the last run. The cursor
is now at the ‘QUANTITY:’ parameter. For our
example, we’ll process a quantity of ten (10) kits, as
programmed (Kit #1). When a kit quantity is entered,
the machine will output kits continuously until the
entered quantity of kits has been processed. The
operator presses the <1> key, the <0> key, then
the <ENTER> or the <RUN> key. The KIT START
screen displays:
JOG - JOG
CUT - CUT
SAVE - ENTER
START – RUN
MANUAL MODE & SAVE OPERATIONS:
A <JOG> or <+> key press at this screen will
advance material through the feed belts (Manual
Mode) for as long as the key is held. A <-> key press
will reverse material (Manual Mode) for as long as
the key is held.
being processed. The fourth (bottom) line (‘PIECES
LEFT’) displays the number of pieces left in the
current batch (not the kit) being processed.
During kit processing, the operator can press the
<ESC/PAUSE> key to stop kit processing and
display the KIT ESCAPE screen:
JOG - JOG
CUT - CUT
ABORT - ESC
CONTINUE - RUN
At this point the operator can jog or cut material
manually (see Manual Mode & Save Operations
section above), or continue the kit run by pressing
the <RUN> key. The kit will resume processing
from the point at which it was stopped. Pressing the
<ESC/PAUSE> key from the KIT ESCAPE screen
(ABORT command) brings the operator to the KIT
RUN COMPLETE screen (below). When all kits
have been processed, the KIT RUN COMPLETE
screen displays:
RUN COMPLETE KIT #1
KITS LEFT 0
A <CUT> key press will cycle the blade once
(Manual Mode).
An <ENTER> key press saves the kit and brings the
operator back to the BATCH SELECT screen.
Continuing our example of 10 kits of Kit #1, the
operator presses the <RUN> key at the KIT
START screen (above). As soon as the <RUN>
key is pressed, kit processing begins, and the KIT
PROCESSING STATUS screen displays:
# OF KITS 10 KIT #1
KITS LEFT X
CURRENT BATCH Y
PIECES LEFT Z
During Automode Kit Processing (running a quantity
of kits) the KIT PROCESSING STATUS screen
(above) displays the quantity of kits programmed
and the kit number on the rst (top) line. This line
is static – it will not change during kit processing.
The second line (‘KITS LEFT’) counts down the
number of kits left to be processed. The third line
(‘CURRENT BATCH’) displays the current batch
PUSH ANY KEY
Pressing any key will bring the operator back to the
BATCH SELECT screen. To return to kit processing/
programming from the BATCH SELECT screen,
press the < . > key.
MANUAL (SINGLE) KIT OPERATION:
(Using the default kit quantity of ‘0’)
In Manual Kit Mode, one (1) kit is processed per
<RUN> key press (even though ‘0’ is entered as a
quantity – in this instance, ‘0’ designates Manual
[Single] Kit Mode). After pressing the <ENTER>
or <RUN> key to accept Quantity of ‘0’ in the KIT
QUANTITY screen (above), the KIT START screen
displays (see above).
Continuing our example of manual/single kit
processing of Kit #1, the operator presses the
<RUN> key at the KIT START screen. The SINGLE
KIT MODE RUN screen displays:
# OF KITS 0 KIT#1
PRESS ESC TO BREAK
PRESS RUN TO PROCEED
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 12
MODEL WC601D AUTOMATIC TUBING CUTTER
p 12
Pressing the <ESC/PAUSE> key from this screen
brings the operator to the BATCH SELECT screen.
Following our Manual Mode example, a <RUN>
key press begins kit processing of (1) kit only, and
displays the KIT PROCESSING STATUS screen
(see above).
Once the rst kit is completed in Manual Mode, the
machine waits for input from the operator with the
SINGLE KIT MODE RUN screen:
# OF KITS 1 KIT#1
PRESS ESC TO BREAK
PRESS RUN TO PROCEED
In our example kit (Kit #1), a kit consists of one
6.0” piece, three 8.0” pieces and one 2.0” piece.
Therefore, in the example above, 5 total pieces
would output and then wait for operator input from
the keypad.
Pressing <RUN> again will process another kit, and
the SINGLE KIT MODE RUN screen would display
‘# OF KITS 2’, and so forth.
Pressing the <ESC/PAUSE> key from this screen
brings the operator to the BATCH SELECT screen.
NOTES ON KIT PROGRAMMING & EDITING:
• Batches need to be dened prior to being entered
into a kit.
• Kit quantities must be entered each time a kit is
called up and processed, they are not stored in the
kit’s program or from the last run.
• During Kit programming, you can use the <+> key
to advance to the next batch; or the <-> key to
return to the previous batch.
• During Kit programming, you can use the < . >
(decimal) key to advance to the last batch in the
kit, or the <BACKSPACE> key to return to the rst
batch in the kit.
• Only the batch at the last (greatest number) Index
location may be erased. This batch is always
designated with a “D” as the Allowable Action
Indicator code (see table above).
• To delete the last batch in a kit, rst display the
batch within the kit, then press the <CUT> key.
The ‘SELECT BATCH’ parameter will change to “0”
and the Allowable Action Indicator code (see table
above) will change to “A”, indicating that a batch
can be added.
• A total of 50 kits may be entered into memory,
depending on memory usage.
BLADE CHANGE/ADJUSTMENT PROCEDURE:
! CAUTION:
•BESUREUNITISUNPLUGGEDBEFORE
CHANGING BLADES OR BELTS.
•BLADESAREEXTREMELYSHARP,HANDLE
CAREFULLY TO PREVENT INJURY.
Please refer to the drawing on page 16 for
clarication on this procedure.
BLADE CHANGE:
To replace the blade, rst remove the front cover,
then remove the exit bushing. Next, remove one of
the two screws holding the blade in place using and
loosen the other one. Slide the blade out from under
the remaining screw and washer. Replace blade,
screw, and tighten. Reinstall exit bushing.
NOTE: If this is the rst time the blade has been
used, it may be used again by turning the blade
around and using the other side. The cutting edge of
the blade is offset from center, so that the blade may
be used twice.
BLADE ADJUSTMENT:
To adjust the depth of the blade, locate the blade
stop adjusting screw located on the rotary head and
loosen the locking set screw.
Blade depth is properly set when the blade stops
slightly deeper than the inside diameter of the tubing
being cut.
Adjust the blade stop adjusting screw counterclockwise to allow the blade to cut deeper, and
clockwise to stop the blade sooner.
Once blade depth has been set, tighten the locking
set screw.
NOTE: NEVER ALLOW THE BLADE TO GO PAST
CENTER OF THE BUSHING.
FEED BELT REPLACEMENT:
Please refer to the drawing on page 15 for
clarication on this procedure.
Loosen the set screws on the feed belt pulleys. Slide
the pulleys and belts together from the spindles.
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 13
MODEL WC601D AUTOMATIC TUBING CUTTER
p 13
Slide the new belt onto the pulleys rst, then reinstall
pulleys and belts together on spindles and tighten
the set screws onto the ats of the spindles.
IMPORTANT: NO LIABILITY WILL BE INCURRED
BY THE ERASER CO. FOR INJURY, DEATH, OR
PROPERTY DAMAGE CAUSED BY A PRODUCT
WHICH HAS BEEN SET UP, OPERATED, AND/OR
INSTALLED CONTRARY TO ERASER’S WRITTEN
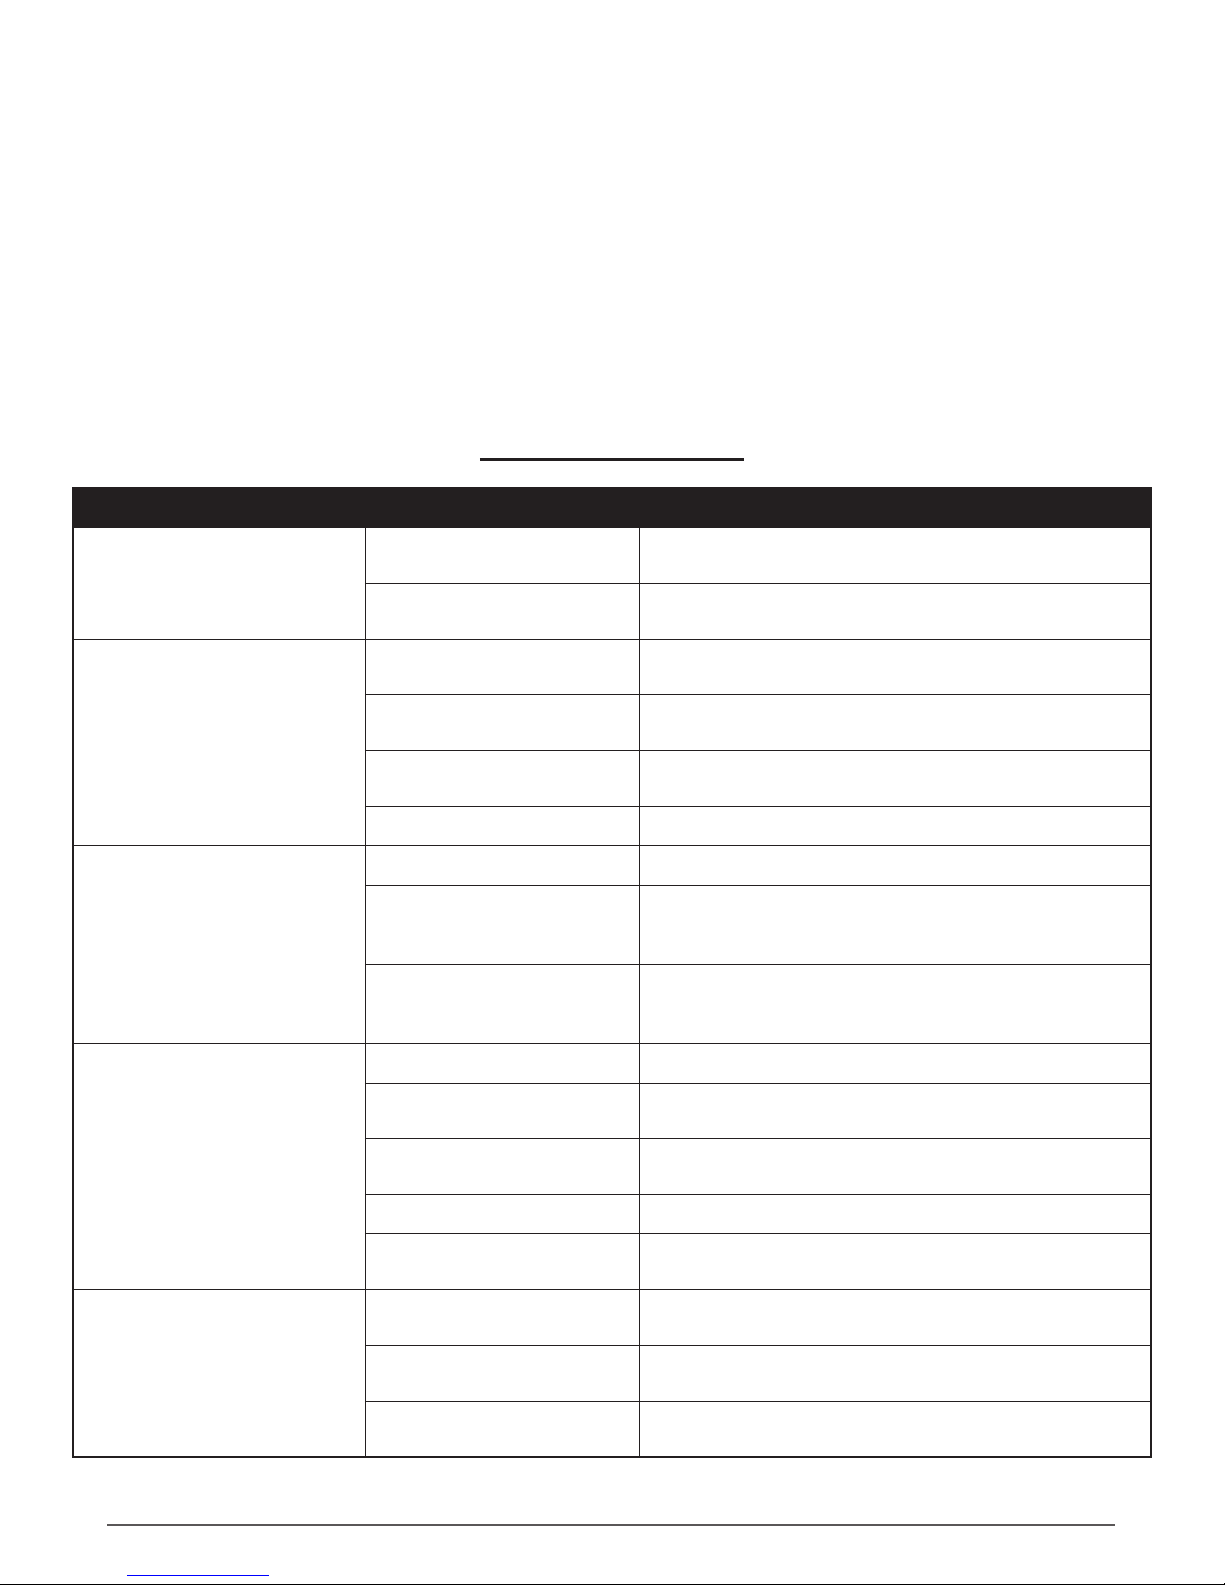
TROUBLESHOOTING
PROBLEM
BLADE STUCK IN THE
CLOSED POSITION
MATERIAL NOT FEEDING
PROPERLY
POSSIBLE CAUSE POSSIBLE SOLUTION
Blade hitting the head
bushing
Blade return spring worn or
broken
Belt feed not adjusted
correctly
Blade stuck in the closed
position
Improper size bushings
OPERATING MANUAL, OR WHICH HAS BEEN
SUBJECTED TO MISUSE, NEGLIGENCE, OR
ACCIDENT, OR WHICH HAS BEEN REPAIRED
OR ALTERED BY ANYONE OTHER THAN THE
ERASER COMPANY, OR WHICH HAS BEEN
USED IN A MANNER OR FOR A PURPOSE FOR
WHICH THE PRODUCT WAS NOT DESIGNED.
TROUBLESHOOTING
Re-Install head bushing; See “Bushing Installation”
Remove and replace worn or broken blade return
spring; See “Replacement Parts”
Re-adjust belt feed tension; See “Unit Operation”
See above PROBLEM (this table): “Blade stuck in the
closed position”
Send in sample material to Eraser for proper bushing
sizing
DISPLAY NOT FUNCTIONING
POOR QUALITY OF CUT OR
NO CUT
INCONSISTENT CUT
LENGTHS
Uneven Dereeler tension Make certain dereeler is functioning properly
Unit not powered up Make sure unit is plugged in & switched on
Replace with recommended fuse; See “Replacement
Blown fuse
Incorrect voltage supplied
Dull or chipped blades See “Blade Change/Adjustment Procedure”
Blade depth needs to be
increased
Improper Cut Speed
Improper Cut Time Increase Cut Time; See “Programming Batches”
Head bushing not installed
correctly
Uneven Dereeler tension
Belt feed tension is loose
Improper size bushings
Parts”
NOTE: If fuse blows more than once, contact factory.
Make certain the incoming voltage is correct and is not
being inuenced by large equipment connected to the
same circuit
Increase the blade depth. See “Blade Change/Adjusting
Procedure”
Reduce or increase Cut Rate; See “Programming
Batches”
Re-Install head bushing; See “Bushing Installation”
At high feed speeds, a power assisted dereeler is
recommended
Tighten the belt feed adjusting knob clockwise to
increase tension
Send in sample material to Eraser for proper bushing
sizing
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 14
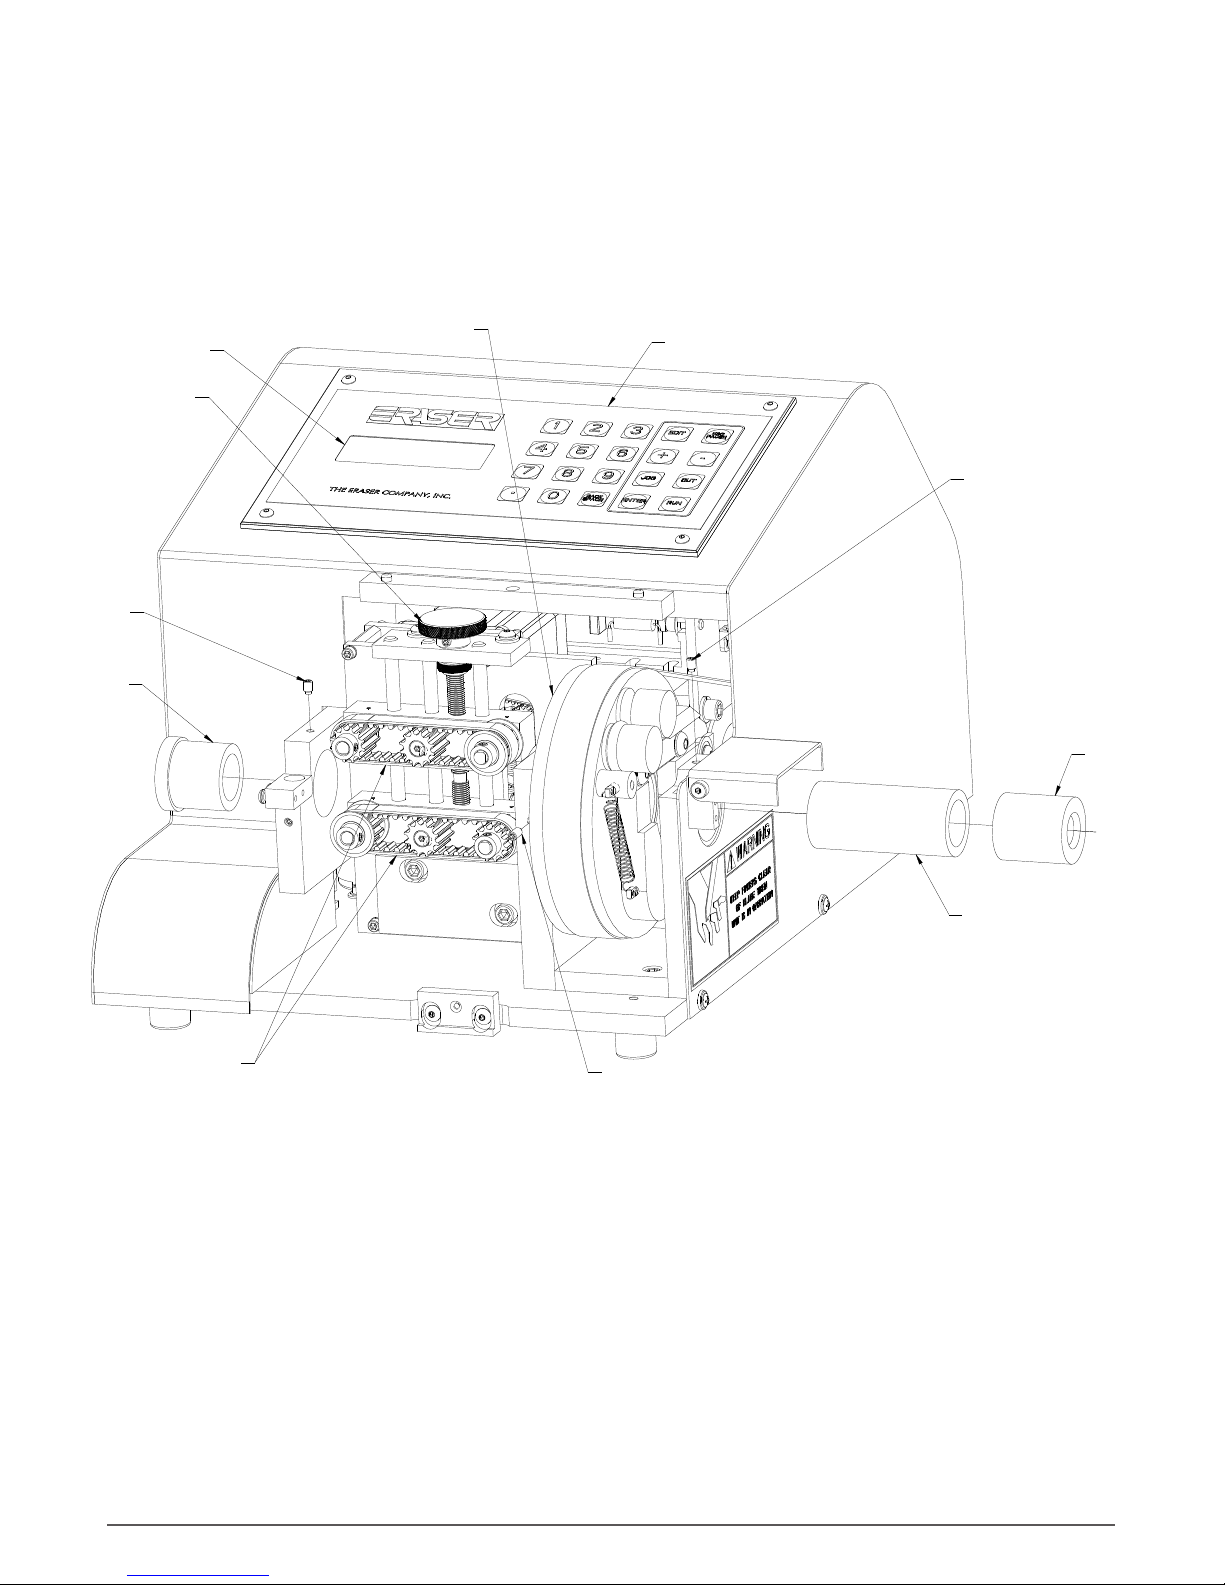
MODEL WC601D AUTOMATIC TUBING CUTTER
Material Bushing(s) Details
p 14
FOUR LINE DISPLAY
TENSION ADJUSTER
ENTRANCE
BUSHING
SET SCREW
ENTRANCE
BUSHING
FEED ROLLER
CUTTING HEAD
KEYPAD
EXIT BUSHING
SET SCREW
EXIT BUSHING
FEED BELTS
HEAD BUSHING
SET SCREW
(SHOWN WITH COVER REMOVED)
HEAD BUSHING
Eraser Company Inc. • Syracuse, NY USA • Ph: 315-454-3237 • [email protected] • www.eraser.com • Fax 315-454-3090
Page 15
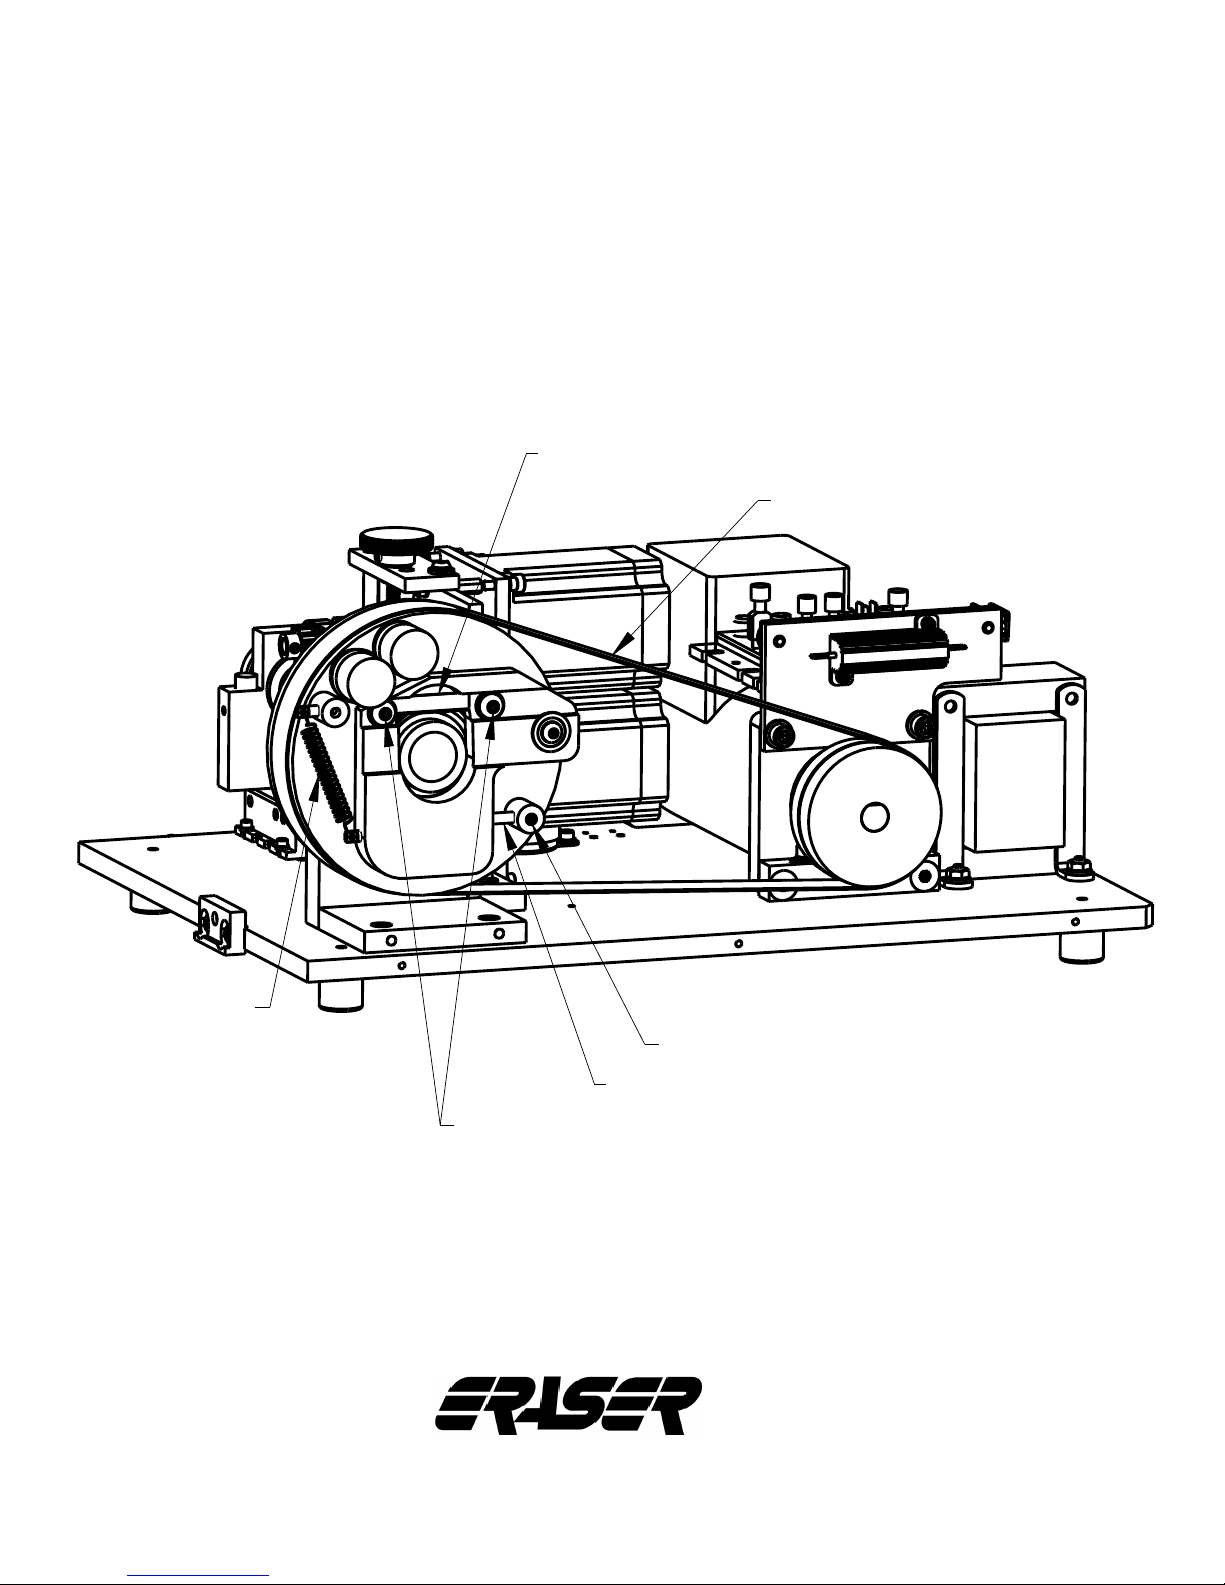
Model WC601D Automatic Tubing Cutter
Cutting Head Blade Details
CUTTING BLADE
DRIVE BELT
p 15
BLADE RETURN SPRING
(SHOWN WITH COVER, HOUSING, GUARD, EXIT BUSHING AND EXIT BUSHING SUPPORT REMOVED)
The Eraser Company, Inc.
PO Box 4961/ Oliva Drive
Syracuse, NY 13221, USA
BLADE STOP ADJUSTING SCREW
BLADE RETENTION SCREWS
Always Moving Forward
LOCKING SET SCREW
®
Phone: (315) 454-3237
Fax: (315) 454-3090
Website: www.eraser.com
E-mail: info@eraser.com
IR1858
REV 10/15
 Loading...