

Page 1
INTEGRATED CIRCUITS
DATA SH EET
SAB6456
SAB6456T
Sensitive 1 GHz
divide-by-64/divide-by-256
switchable prescaler
Product specification
File under Integrated Circuits, IC02
June 1986
Page 2
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
GENERAL DESCRIPTION
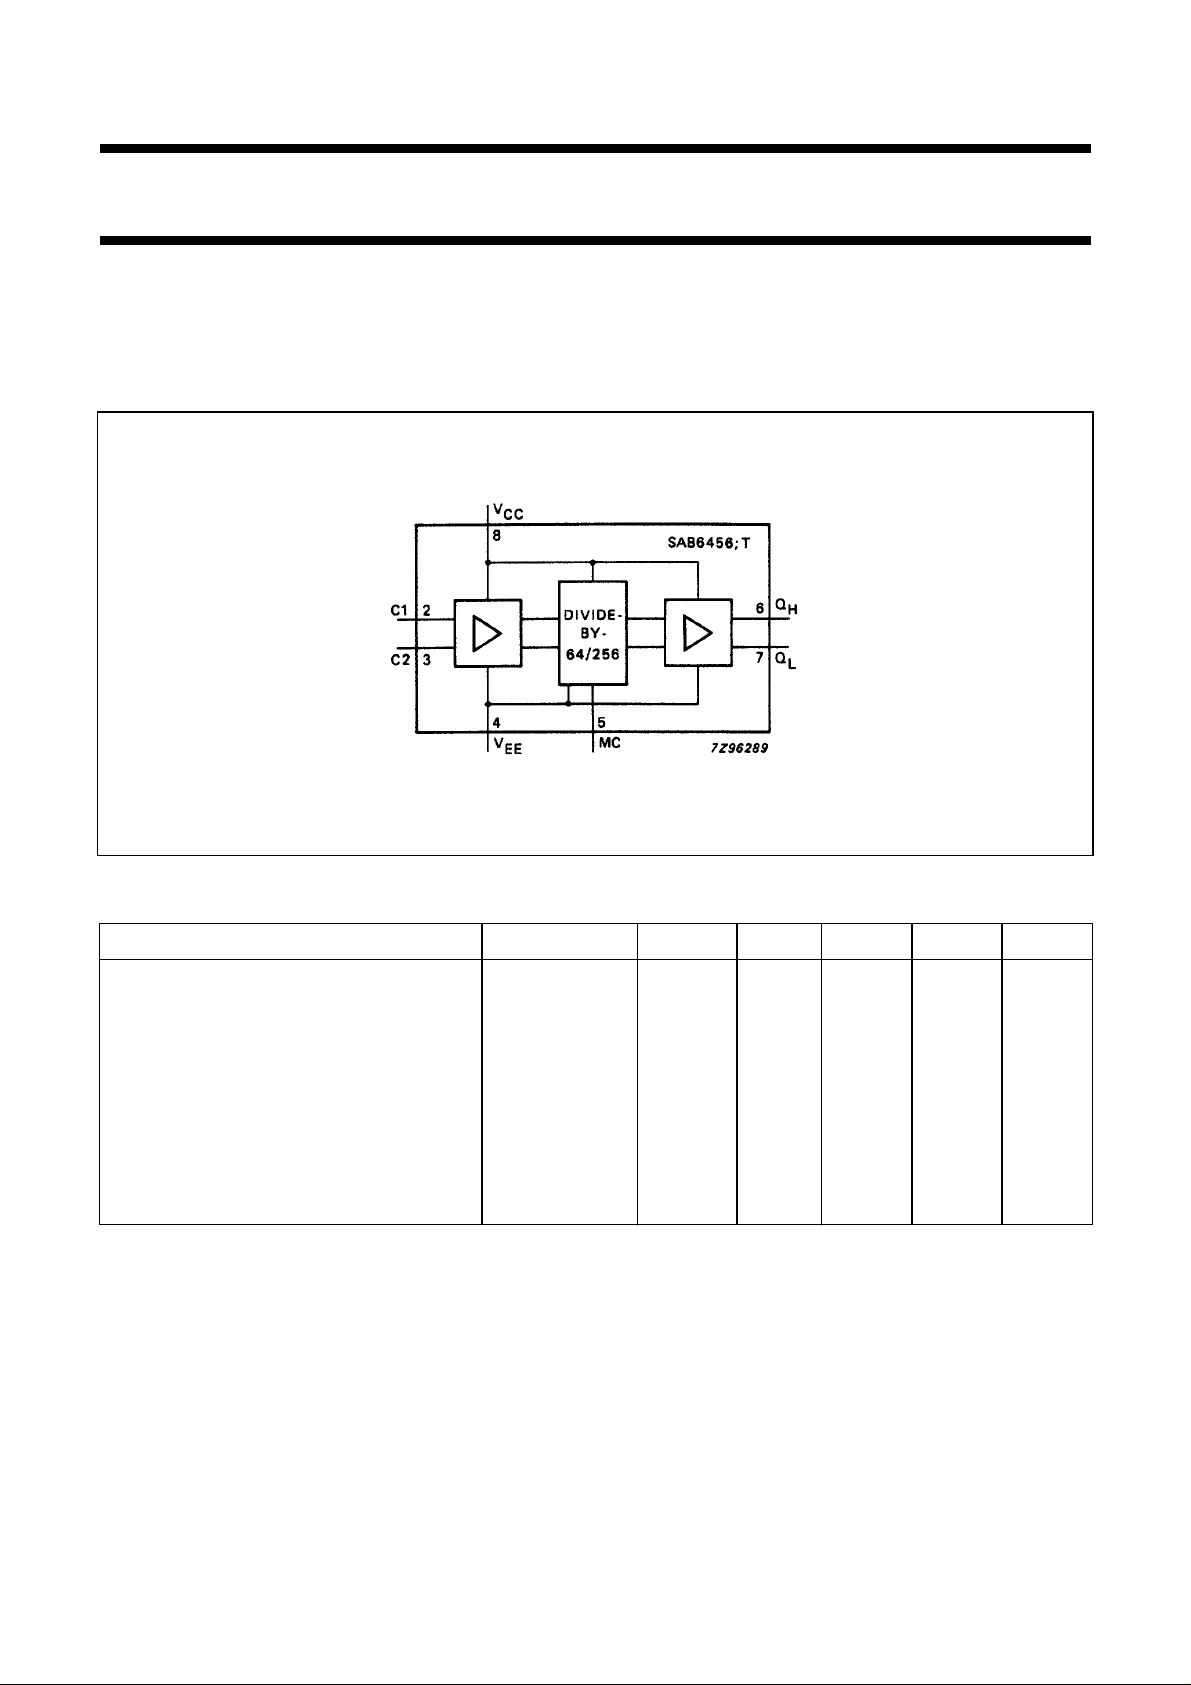
The SAB6456/SAB6456T is a prescaler for UHF/VHF tuners. It can be switched to divide-by-64 or divide-by-256 by the
mode-control (MC) pin. The circuit has an input frequency range of 70 MHz to 1 GHz, has high input sensitivity and good
harmonic suppression.
SAB6456
SAB6456T
Fig.1 Block diagram.
QUICK REFERENCE DATA
PARAMETER CONDITIONS SYMBOL MIN. TYP. MAX. UNIT
Supply voltage pin 8 to pin 4 V
Supply current pin 8 I
Input frequency range pins 2 and 3 f
Sensitivity to input voltage
(r.m.s. value) V
Output voltage
(peak-to-peak value) pins 6 and 7 V
Operating ambient
temperature range T
PACKAGE OUTLINES
SAB6456 : 8-lead DIL; plastic (SOT97); SOT97-1; 1996 November 18.
SAB6456T: 8-lead mini-pack (SO8; SOT96A); SOT96-1; 1996 November 18.
CC
CC
i
i(rms)
o(p-p)
amb
4,5 5,0 5,5 V
− 21 − mA
70 − 1000 MHz
−− 10 mV
− 1 − V
0 − 80 °C
June 1986 2
Page 3
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
PINNING
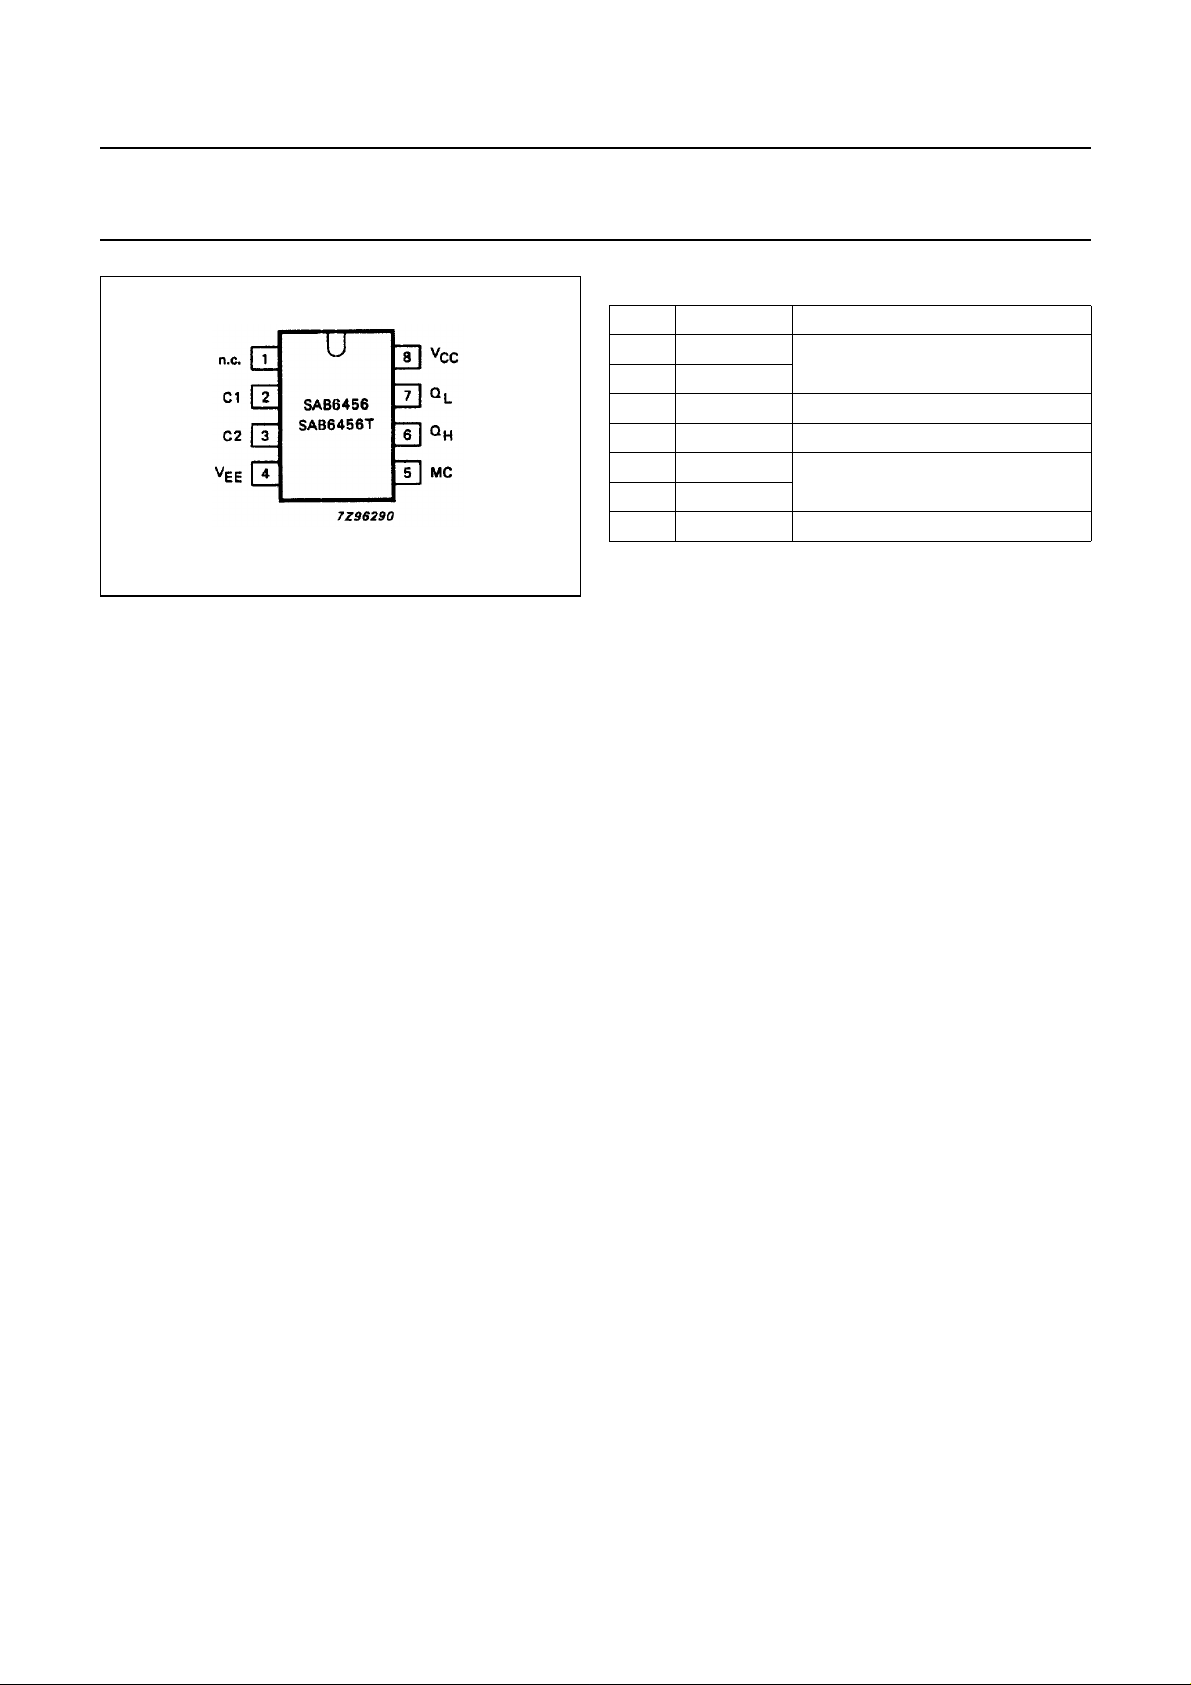
1. n.c. not connected
2. C1
3. C2
4. V
5. MC mode control
6. Q
7. Q
8. V
Fig.2 Pinning diagram.
FUNCTIONAL DESCRIPTION
The circuit comprises an input amplifier, a divider stage with selectable division ratio and an output stage.
The input amplifier is driven by a sinusoidal signal from the local oscillator of a television tuner. The inputs (C1, C2) are
differential and are biased internally to permit capacitive coupling. When driven asymmetrically the unused input should
be connected to ground via a capacitor.
EE
H
L
CC
differential inputs
ground (0 V)
complementary outputs
positive supply voltage
SAB6456
SAB6456T
The mode-control (MC) input to the divider stage is intended for static control of the division ratio, selection is made as
follows:
divide-by-64: MC pin open-circuit
divide-by-256: MC pin connected to ground
The divider stage may oscillate during no-signal conditions but this oscillation is suppressed when input signals are
received.
Two complementary signals (Q
output signals are slowed internally to reduce harmonics in the television intermediate frequency band.
, QL) are provided by the output differential amplifier stage. The voltage-edges of the
H
June 1986 3
Page 4
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
ELECTROSTATIC DISCHARGE PROTECTION
Inputs and outputs have electrostatic discharge protection according to specification MIL-883C, class B.
RATINGS
Limiting values in accordance with the Absolute Maximum System (IEC-134)
PARAMETER CONDITIONS SYMBOL MIN. TYP. MAX. UNIT
Supply voltage pin 8 to pin 4 V
Input voltage V
Storage temperature range T
Junction temperature T
CC
i
stg
j
THERMAL RESISTANCE
From junction to ambient
8-lead DIL; plastic (SOT-97A) R
8-lead mini-pack (SO-8; SOT-96A)
on printed circuit board R
on ceramic substrate R
−−7,0 V
−−VCCV
−55 −+150 ° C
−−+150 ° C
SAB6456T
th j-a
th j-a
th j-a
SAB6456
120 K/W
260 K/W
170 K/W
D.C. CHARACTERISTICS
=5V; VEE=0V; T
V
CC
=25°C; test IC mounted in a test socket or on a printed circuit board; measurements taken
amb
after thermal equilibrium is established
PARAMETER CONDITIONS SYMBOL MIN. TYP. MAX. UNIT
Output voltage HIGH V
Output voltage LOW V
Supply current I
Mode-control (MC)
Input voltage LOW
(divide-by-256) V
Input current LOW −I
Input voltage HIGH
(divide-by-64) pin 5 open-circuit V
CC
OH
OL
IL
L
IH
−−VCCV
−−V
− 0.8 V
CC
− 21 28 mA
0 − 0,2 V
− 25 60 µA
1,4 − 3,0 V
June 1986 4
Page 5
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
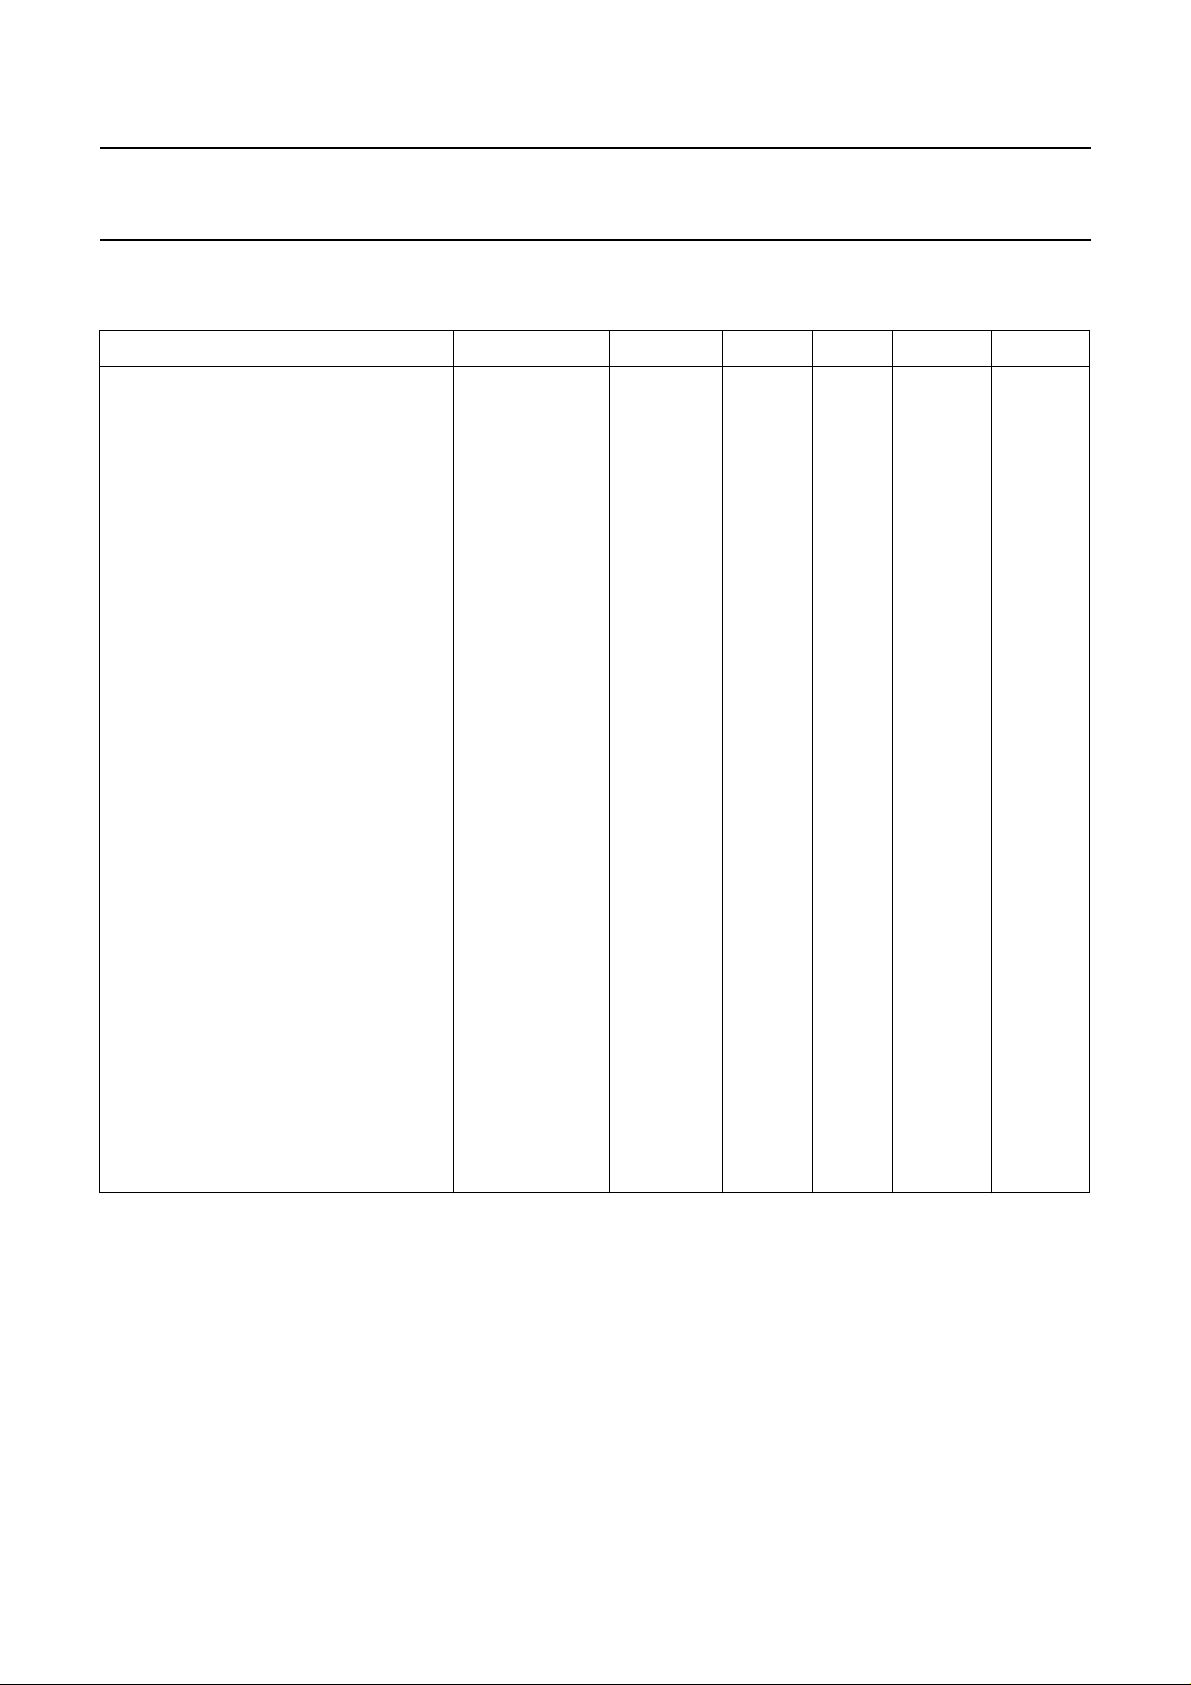
A.C. CHARACTERISTICS
V
= 4,5 to 5,5 V; VEE=0V; T
CC
PARAMETER CONDITIONS SYMBOL MIN. TYP. MAX. UNIT
Sensitivity to input 50 Ω system
voltage (r.m.s. value) f
Input overload voltage 50 Ω system
(r.m.s. value) f
Input parallel resistance f
Input capacitance f
Output voltage HIGH V
Output voltage LOW V
= 0 to +80 °C
amb
= 70 MHz V
i
f
= 150 MHz V
i
= 300 MHz V
f
i
f
= 500 MHz V
i
f
= 900 MHz V
i
= 1000 MHz V
f
i
= 70 MHz to
i
1000 MHz V
= 70 MHz R
i
f
= 1000 MHz R
i
= 70 MHz C
i
= 1000 MHz C
f
i
i(rms)
i(rms)
i(rms)
i(rms)
i(rms)
i(rms)
i
i
i
i
i
OH
OL
SAB6456
SAB6456T
−−10 mV
−−10 mV
−−10 mV
−−10 mV
−−10 mV
−−10 mV
300 −− mV
− 560 −Ω
− 30 −Ω
− 5 − pF
− 1,5 − pF
−−VCCV
−−V
− 0,8 V
CC
Output voltage swing
(peak-to-peak value) f
= 70 MHz V
i
f
= 1000 MHz;
i
R
= 820 Ω;
L
=60pF V
C
L
Attenuation of third
harmonic at output f
= 800 MHz;
i
R
= 820 Ω;
L
=60pF −15 −23 − dB
C
L
Output unbalance see Fig.3 ∆V
Output resistance R
o(p-p)
o(p-p)
o
o
0,8 1,0 1,2 V
0,17 −− V
−−0,1 V
− 500 −Ω
June 1986 5
Page 6
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
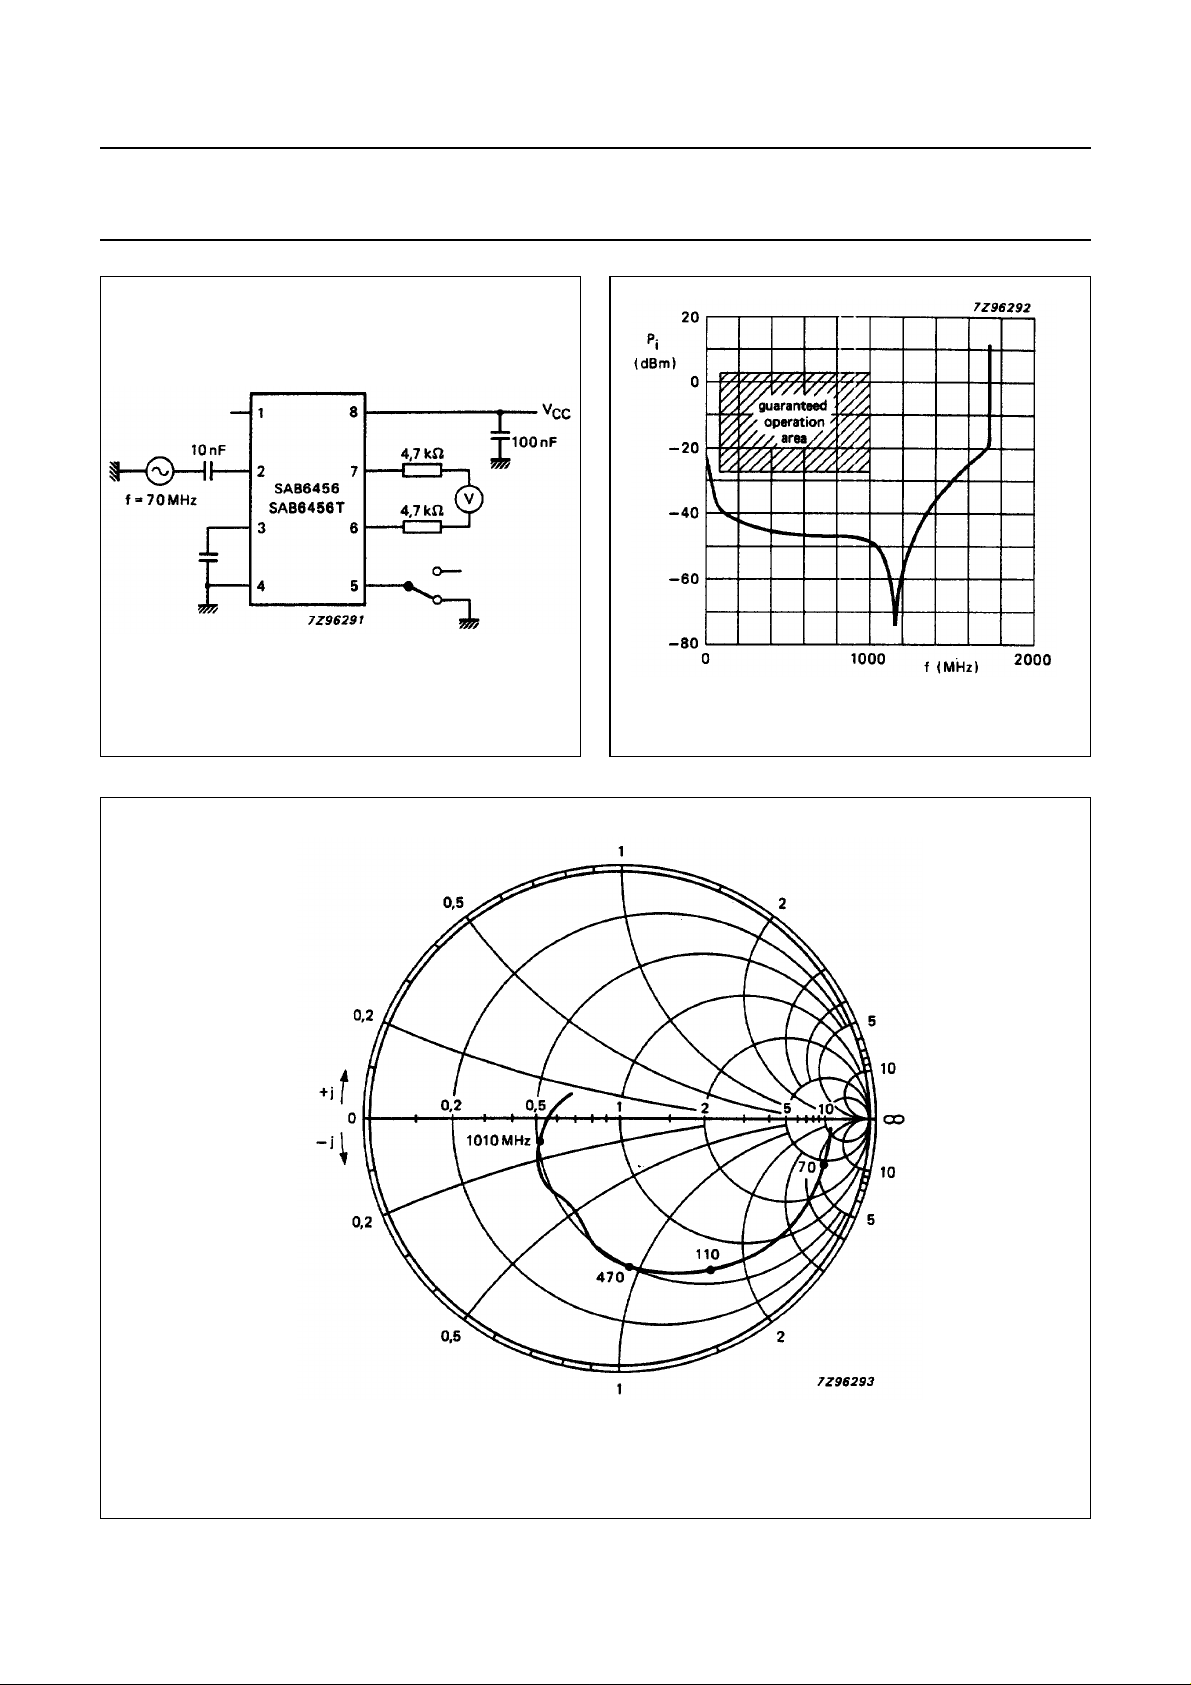
Fig.3 Test circuit for output unbalance measurement.
SAB6456
SAB6456T
Fig.4 Typical input sensitivity curve: VCC=5V;
T
=25°C.
amb
Fig.5 Smith chart of typical input impedance: V
June 1986 6
= 25 mV; VCC= 5 V; reference value = 50 Ω.
i(rms)
Page 7
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
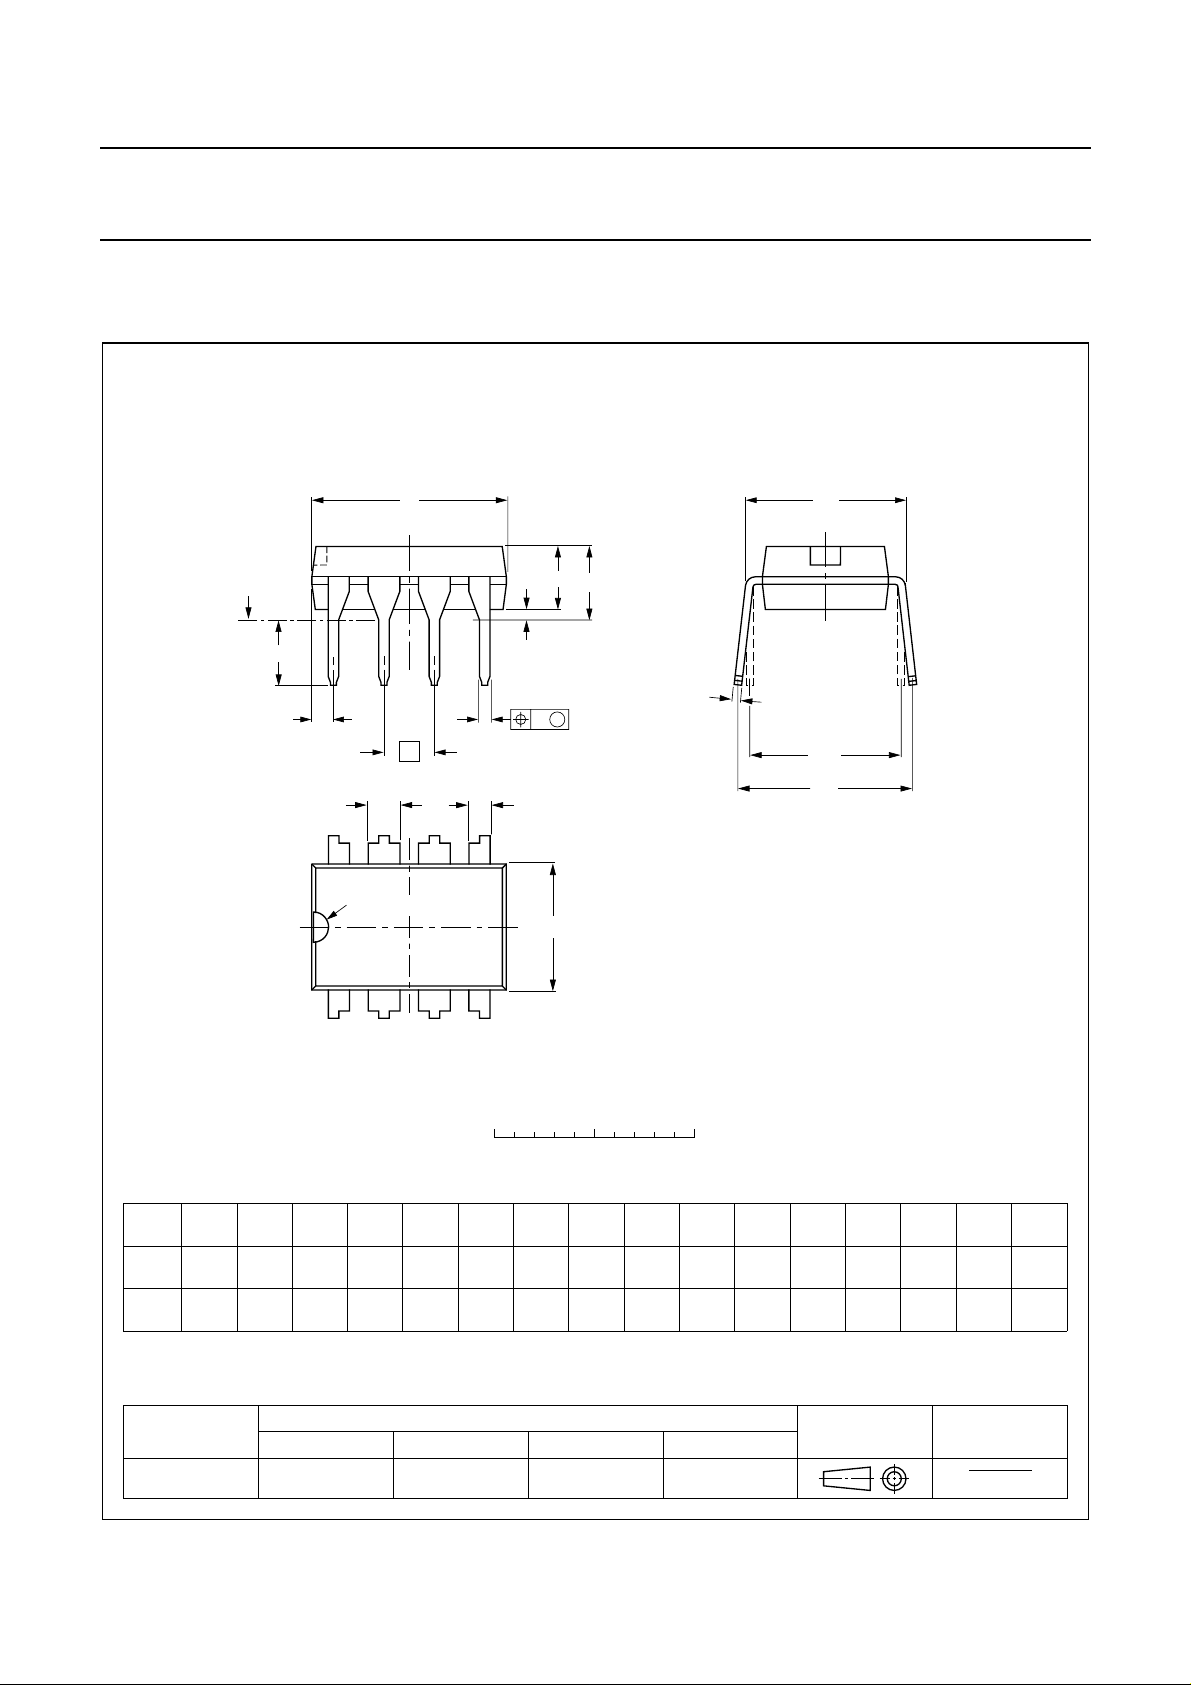
PACKAGE OUTLINES
DIP8: plastic dual in-line package; 8 leads (300 mil)
D
A
2
seating plane
L
Z
A
b
e
b
8
1
b
5
A
1
w M
2
SAB6456
SAB6456T
SOT97-1
M
E
c
(e )
1
M
H
pin 1 index
E
1
DIMENSIONS (inch dimensions are derived from the original mm dimensions)
A
A
A
UNIT
max.
mm
inches
Note
1. Plastic or metal protrusions of 0.25 mm maximum per side are not included.
OUTLINE
VERSION
SOT97-1
12
min.
max.
050G01 MO-001AN
b
1.73
1.14
0.068
0.045
IEC JEDEC EIAJ
0.021
0.015
b
1
0.53
0.38
4
0 5 10 mm
scale
b
2
0.36
1.07
0.23
0.89
0.014
0.042
0.009
0.035
REFERENCES
(1) (1)
cD E e M
9.8
9.2
0.39
0.36
6.48
6.20
0.26
0.24
L
e
1
M
3.60
8.25
3.05
7.80
0.14
0.32
0.12
0.31
EUROPEAN
PROJECTION
E
10.0
0.39
0.33
H
8.3
w
max.
0.2542.54 7.62
ISSUE DATE
0.010.10 0.30
92-11-17
95-02-04
1.154.2 0.51 3.2
0.0450.17 0.020 0.13
(1)
Z
June 1986 7
Page 8
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
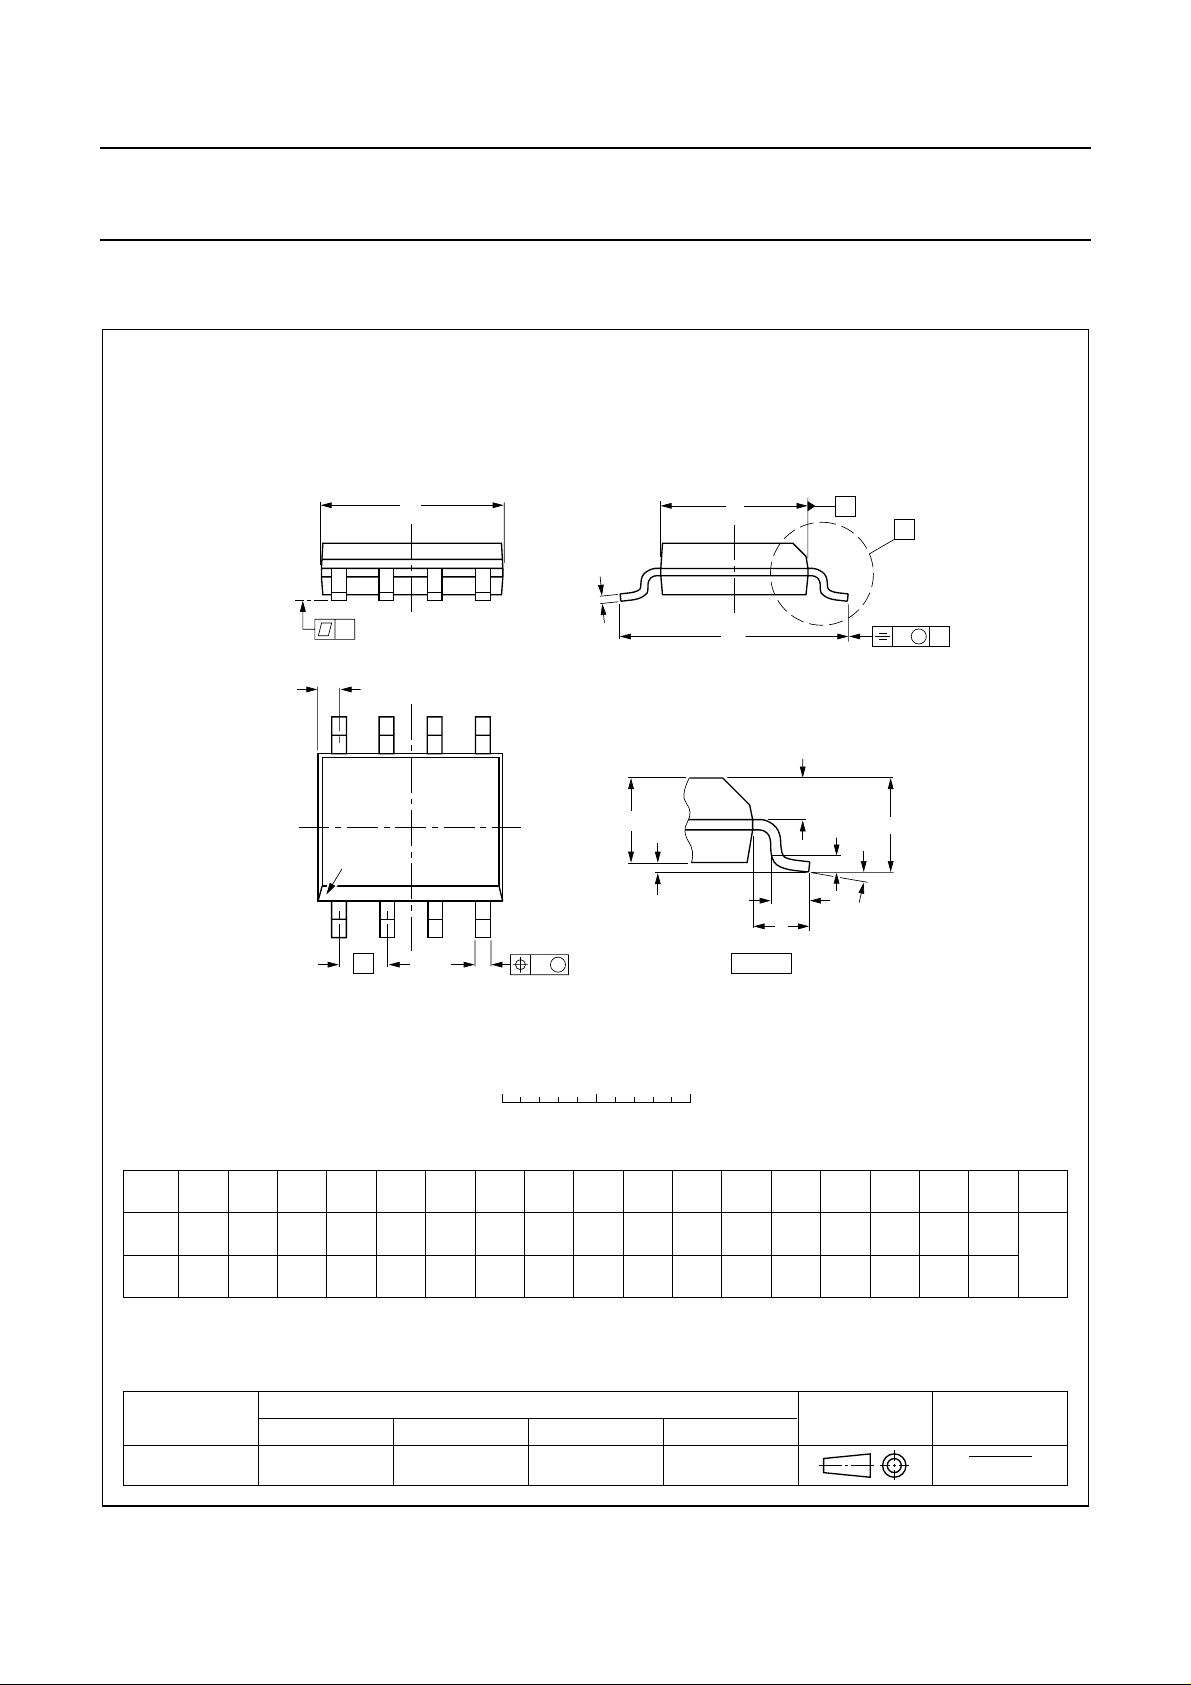
SO8: plastic small outline package; 8 leads; body width 3.9 mm
D
c
y
Z
8
5
SAB6456
SAB6456T
SOT96-1
E
H
E
A
X
v M
A
A
pin 1 index
1
e
DIMENSIONS (inch dimensions are derived from the original mm dimensions)
UNIT
mm
inches
Notes
1. Plastic or metal protrusions of 0.15 mm maximum per side are not included.
2. Plastic or metal protrusions of 0.25 mm maximum per side are not included.
A
max.
1.75
0.069
A1A2A
0.25
1.45
0.10
1.25
0.010
0.057
0.004
0.049
0.25
0.01
b
3
p
0.49
0.25
0.36
0.19
0.019
0.0100
0.014
0.0075
4
w M
b
p
0 2.5 5 mm
scale
(1)E(2)
cD
5.0
4.8
0.20
0.19
0.16
0.15
eHELLpQZywv θ
4.0
1.27
3.8
0.050
2
A
6.2
5.8
0.244
0.228
Q
3
A
θ
0.25 0.10.25
0.010.010.041 0.004
(1)
0.7
0.3
0.028
0.012
o
8
o
0
L
p
L
0.7
0.6
0.028
0.024
(A )
1
detail X
1.0
1.05
0.4
0.039
0.016
OUTLINE
VERSION
SOT96-1
IEC JEDEC EIAJ
076E03S MS-012AA
REFERENCES
June 1986 8
EUROPEAN
PROJECTION
ISSUE DATE
95-02-04
97-05-22
Page 9
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
SOLDERING
Introduction
There is no soldering method that is ideal for all IC
packages. Wave soldering is often preferred when
through-hole and surface mounted components are mixed
on one printed-circuit board. However, wave soldering is
not always suitable for surface mounted ICs, or for
printed-circuits with high population densities. In these
situations reflow soldering is often used.
This text gives a very brief insight to a complex technology.
A more in-depth account of soldering ICs can be found in
our
“IC Package Databook”
DIP
SOLDERING BY DIPPING OR BY WA VE
The maximum permissible temperature of the solder is
260 °C; solder at this temperature must not be in contact
with the joint for more than 5 seconds. The total contact
time of successive solder waves must not exceed
5 seconds.
The device may be mounted up to the seating plane, but
the temperature of the plastic body must not exceed the
specified maximum storage temperature (T
printed-circuit board has been pre-heated, forced cooling
may be necessary immediately after soldering to keep the
temperature within the permissible limit.
R
EPAIRING SOLDERED JOINTS
Apply a low voltage soldering iron (less than 24 V) to the
lead(s) of the package, below the seating plane or not
more than 2 mm above it. If the temperature of the
soldering iron bit is less than 300 °C it may remain in
contact for up to 10 seconds. If the bit temperature is
between 300 and 400 °C, contact may be up to 5 seconds.
SO
REFLOW SOLDERING
Reflow soldering techniques are suitable for all SO
packages.
(order code 9398 652 90011).
). If the
stg max
SAB6456
SAB6456T
Several techniques exist for reflowing; for example,
thermal conduction by heated belt. Dwell times vary
between 50 and 300 seconds depending on heating
method. Typical reflow temperatures range from
215 to 250 °C.
Preheating is necessary to dry the paste and evaporate
the binding agent. Preheating duration: 45 minutes at
45 °C.
AVE SOLDERING
W
Wave soldering techniques can be used for all SO
packages if the following conditions are observed:
• A double-wave (a turbulent wave with high upward
pressure followed by a smooth laminar wave) soldering
technique should be used.
• The longitudinal axis of the package footprint must be
parallel to the solder flow.
• The package footprint must incorporate solder thieves at
the downstream end.
During placement and before soldering, the package must
be fixed with a droplet of adhesive. The adhesive can be
applied by screen printing, pin transfer or syringe
dispensing. The package can be soldered after the
adhesive is cured.
Maximum permissible solder temperature is 260 °C, and
maximum duration of package immersion in solder is
10 seconds, if cooled to less than 150 °C within
6 seconds. Typical dwell time is 4 seconds at 250 °C.
A mildly-activated flux will eliminate the need for removal
of corrosive residues in most applications.
R
EPAIRING SOLDERED JOINTS
Fix the component by first soldering two diagonallyopposite end leads. Use only a low voltage soldering iron
(less than 24 V) applied to the flat part of the lead. Contact
time must be limited to 10 seconds at up to 300 °C. When
using a dedicated tool, all other leads can be soldered in
one operation within 2 to 5 seconds between
270 and 320 °C.
Reflow soldering requires solder paste (a suspension of
fine solder particles, flux and binding agent) to be applied
to the printed-circuit board by screen printing, stencilling or
pressure-syringe dispensing before package placement.
June 1986 9
Page 10
Philips Semiconductors Product specification
Sensitive 1 GHz divide-by-64/divide-by-256
switchable prescaler
DEFINITIONS
Data sheet status
Objective specification This data sheet contains target or goal specifications for product development.
Preliminary specification This data sheet contains preliminary data; supplementary data may be published later.
Product specification This data sheet contains final product specifications.
Limiting values
Limiting values given are in accordance with the Absolute Maximum Rating System (IEC 134). Stress above one or
more of the limiting values may cause permanent damage to the device. These are stress ratings only and operation
of the device at these or at any other conditions above those given in the Characteristics sections of the specification
is not implied. Exposure to limiting values for extended periods may affect device reliability.
Application information
Where application information is given, it is advisory and does not form part of the specification.
LIFE SUPPORT APPLICATIONS
These products are not designed for use in life support appliances, devices, or systems where malfunction of these
products can reasonably be expected to result in personal injury. Philips customers using or selling these products for
use in such applications do so at their own risk and agree to fully indemnify Philips for any damages resulting from such
improper use or sale.
SAB6456
SAB6456T
June 1986 10
 Loading...