

Page 1
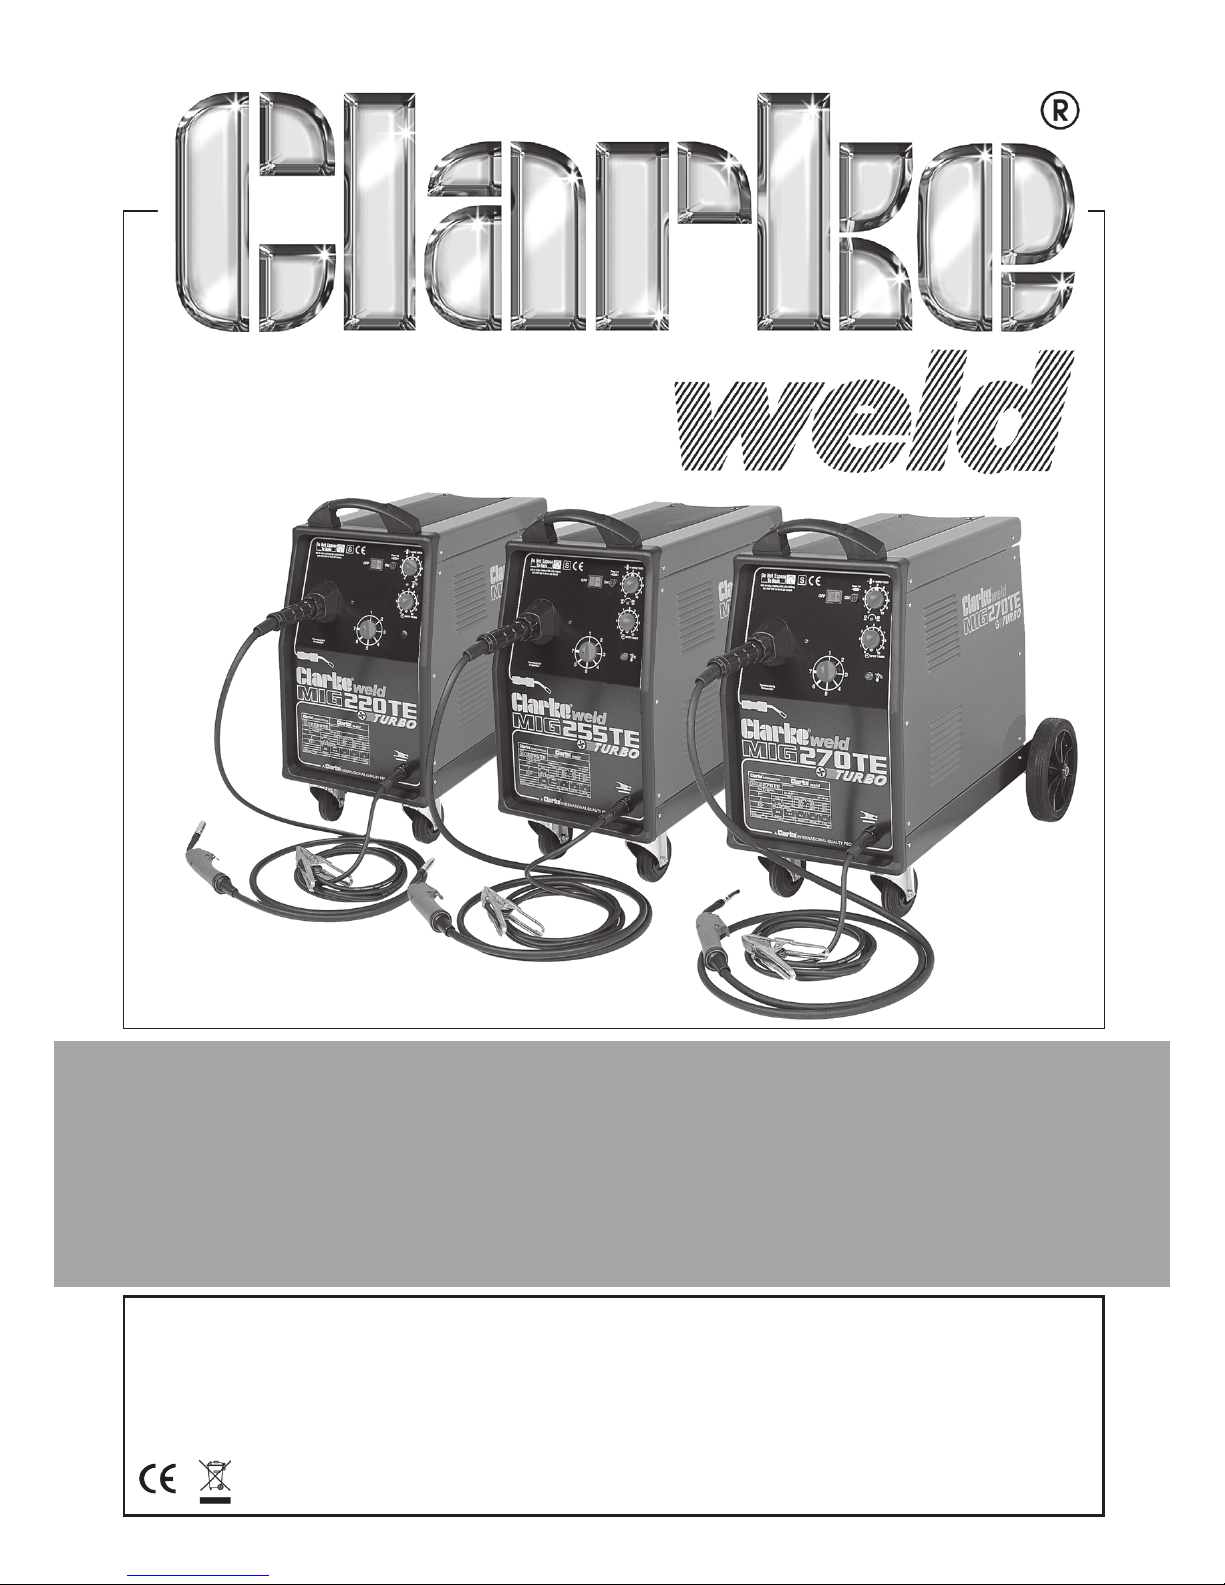
OPERATING & MAINTENANCE
INSTRUCTIONS
11/16
MIG220TE, MIG255TEC &
MIG270TE WELDERS
Page 2
2
INTRODUCTION
Thank you for purchasing this CLARKE MIG Welder.
Before attempting to operate the machine, it is essential that you read this manual thoroughly
and carefully follow all instructions given. In doing so you will ensure the safety of yourself and
that of others around you, and you can also look forward to the welder giving you long and
satisfactory service.
GUARANTEE
This CLARKE product is guaranteed against faulty manufacture for a period of 12 months from
the date of purchase. Please keep your receipt as proof of purchase.
This guarantee is invalid if the product is found to have been abused or tampered with in any
way, or not used for the purpose for which it was intended.
Faulty goods should be returned to their place of purchase, no product can be returned to us
without prior permission.
This guarantee does not effect your statutory rights.
Please note that the details and specifications contained herein, are correct at the time of
going to print. However, CLARKE International reserve the right to change specifications at any
time without prior notice. ALWAYS CONSULT THE MACHINE’S DATA PLATE
* Duty Cycle: Determines the machine ‘down time’.
SPECIFICATIONS
220TE TURBO 255TEC TURBO 270TE TURBO
Power Supply 230V 50Hz 1Ph 230V 50Hz 1Ph 400V 50Hz 3Ph
Main Fuse Rating 25 Amps 40 Amps 16 Amps
Current Range 40-200A 30-250A 30-260A
Max. Metal Thickness (m/s) 10-11mm 10-11mm 10-11mm
Welding Wire Sizes 0.6-0.8mm 0.6-0.8mm 0.6-0.8mm
Duty Cycle* 20% 200A --
30% - 250A -
35% - - 260A
60% 123A 150A 170A
100% 95A 140A 135A
Dimensions (no handle) mm 740x830x500 740x830x500 740x830x500
Weight 71 kg 79 kg 79 kg
Part No. 6015220 6015510 6015240
Page 3
3
CONTENTS
Guarantee .............................................................................................. 2
Specifications ........................................................................................ 2
General Safety Precautions for all Welding ........................................ 4
Additional Safety Precautions for MIG Welding ................................. 8
Electromagnetic Interference (EMC) ................................................. 9
Electrical Connections .......................................................................11
Principles of MIG Welding ................................................................... 12
Declaration of Conformity ..................................................................12
Unpacking and Parts Identification ................................................... 13
General Layout .................................................................................... 14
Assembly .............................................................................................. 15
Preparation for Use .............................................................................. 17
Operation .............................................................................................20
General Information ..................................................................... 23
Welding Tips .......................................................................................... 24
Maintenance ....................................................................................... 25
Troubleshooting ...................................................................................26
Wiring Diagrams ...................................................................................27
Parts Lists and Diagrams ......................................................................30
ENVIRONMENTAL RECYCLING POLICY
Through purchase of this product, the customer is taking on the obligation to deal with the WEEE in accordance with the WEEE regulations in
relation to the treatment, recycling & recovery and environmentally
sound disposal of the WEEE.
In effect, this means that this product must not be disposed of with general
household waste. It must be disposed of according to the laws governing
Waste Electrical and Electronic Equipment (WEEE) at a recognised disposal
facility.
Page 4
4
E
GENERAL SAFETY PRECAUTIONS FOR ALL
TYPES OF WELDING
WARNING: As with all machinery, there are certain hazards involved
with their operation and use. Exercising respect and caution will
considerably lessen the risk of personal injury. However, if normal safety
precautions are overlooked, or ignored, personal injury to the operator
may result.
FAILURE TO FOLLOW THESE RULES MAY RESULT IN SERIOUS PERSONAL INJURY
GENERAL PRECAUTIONS
A) Burn prevention
Wear protective clothing - gauntlet gloves designed for use in welding, apron, and protective
shoes. Button shirt collar and pocket flaps, and wear cuffless trousers to avoid entry of sparks
and slag. Wear helmet with safety goggles or glasses with side shields underneath, appropriate
filter lenses or plates (protected by clear glass). This is a MUST for welding (and chipping) to
protect the eyes from radiant energy and spatter. Replace cover glass when broken, pitted, or
spattered. Avoid oily greasy clothing. A spark may ignite them. Hot metal should never be
handled without gloves. First aid facilities and a qualified first aid person should be available
unless medical facilities are close by for immediate treatment of flash burns of the eyes and skin
burns. Ear plugs should be worn when working overhead or in a confined space. A hard hat
should be worn when others work overhead. Flammable hair preparations should not be used by
persons intending to weld or cut.
NOTE: ALL protective wear incl. masks & head shields MUST comply with PPE
Directive 89/686/EEC
B) Toxic fume prevention
Severe discomfort, illness or death can result from fumes, vapours, heat, or oxygen enrichment
or depletion that welding (or cutting) may produce. Prevent them with adequate ventilation.
NEVER ventilate with oxygen. Lead-, cadmium-, zinc-, mercury- and beryllium-, bearing
materials, when welded (or cut) may produce harmful concentrations of toxic fumes. Adequate
local exhaust ventilation must be used, or each person in the area as well as the operator must
wear an air- supplied respirator. For beryllium, both must be used. Metals coated with or
containing materials that emit toxic fumes should not be heated unless coating is removed from
the work surface, the area is well ventilated, or the operator wears an air-supplied respirator.
Work in a confined space only while it is being force ventilated and, if necessary, while wearing
an air-supplied respirator. Vapours from chlorinated solvents can be decomposed by the heat of
the arc (or flame) to form PHOSGENE, a highly toxic gas, and other lung and eye irritating
products. The ultraviolet (radiant) energy of the arc can also decompose trichloroethylene and
perchloroethylene vapours to form phosgene. DO NOT WELD or cut where solvent vapours can
be drawn into the welding or cutting atmosphere or where the radiant energy can penetrate to
atmospheres containing even minute amounts of trichloroethylene or perchloroethylene.
Page 5
5
C) Fire and explosion prevention
Causes of fire and explosion are:
1) combustibles reached by the arc, flame, flying sparks, hot slag or heated material;
2) misuse of compressed gases and cylinders
3) short circuits.
BE AWARE that flying sparks or falling slag can pass through cracks, along pipes, through
windows or doors, and through wall or floor openings, out of sight of the goggled operator.
To prevent fires and explosion: keep equipment clean and operable, free of oil, grease, and (in
electrical parts) of metallic particles that can cause short circuits. If combustibles are in area, do
NOT weld. Move the work if practicable, to an area free of combustibles.
Avoid working in paint spray rooms, dip tanks, storage areas, ventilators. If the work cannot be
moved, move combustibles away from sparks and heat; or protect against ignition with suitable
fire- resistant covers or shields.
Walls, ceilings, and floor near work should be protected by heat resistant covers or shields. Fire
watcher must be standing by with suitable fire extinguishing equipment during and for some time
after welding or cutting if:
a) appreciable combustibles (including building construction) are within 10m.
b) appreciable combustibles are further than 10m, but can be ignited by sparks.
c) openings (concealed or visible) in floors or walls can expose combustibles to sparks.
d) combustibles adjacent to walls, ceilings, roofs or metal partitions can be ignited by
radiant or conducted heat.
After work, check that area is free of sparks, glowing embers, and flames. An empty container
that held combustibles, or that can produce flammable or toxic vapours when heated, must never
be welded on or cut, unless container has first been cleaned. This includes a thorough steam or
caustic cleaning (or a solvent or water washing, depending on the combustible’s solubility)
followed by purging and inerting with nitrogen or carbon dioxide, and using protective equipment.
Water filling just below working level may substitute for inerting.
A container with unknown contents should be cleaned (see paragraph above), do NOT depend on
sense of smell or sight to determine if it is safe to weld or cut. Hollow castings or containers must
be vented before welding or cutting - they can explode.
In explosive atmospheres, never weld or cut where the air may contain flammable dust, gas, or
liquid vapours.
ELECTRIC ARC (MIG, TIG) WELDING
Comply with precautions in above, and this section. Arc welding, properly done, is a safe
process but a careless operator invites trouble. The equipment carries high currents at significant
voltages. The arc is very bright and hot. Sparks fly, fumes rise, ultraviolet and infrared energy
radiates and work pieces are hot. The wise operator avoids unnecessary risks and protects
himself and others from accidents.
Page 6
6
A) BURN PROTECTION
The welding arc is intense and visibly bright. It’s radiation can damage eyes, penetrate
lightweight clothing, reflect from light coloured surfaces and burn the skin and eyes. Skin burns
resemble acute sunburn, those from gas - shielded arcs are more severe and painful.
DON’T GET BURNED! FOLLOW ALL SAFETY PRECAUTIONS!
Protective clothing
Wear long sleeved clothing (particularly for gas shielded arc) in addition to gloves, apron and
strong shoes. As necessary, use additional protective clothing such as leather jacket or sleeves,
flameproof apron, and fire-resistant leggings. Avoid outer garments of untreated cotton. Bare
skin protection: Wear dark substantial clothing, Button collars closed to protect the chest and
neck and button any pockets to prevent entry of sparks.
Eye and head protection
Protect eyes from exposure to arc. NEVER look at an electric arc without protection. Welding
helmet or shield containing an appropriate filter plate (Please refer to the section ‘Welding
Shield). Place over face before striking arc. Protect filter plate with a clear cover plate. Cracked
or broken helmet or shield should NOT be worn; radiation can pass through to cause burns.
Cracked, broken, or loose filter plates must be replaced IMMEDIATELY.Replace clear cover plate
when broken, pitted, or spattered. WE SUGGEST you wear flash goggles with side shields under
the helmet, to give some protection to the eyes should the helmet not be lowered over the face
before an arc is struck. Looking at an arc momentarily with unprotected eyes (particularly a high
intensity gas-shielded arc) can cause a retinal burn thatmay leave a permanent dark area in the
field of vision. Before welding whilst wearing contact lenses, seek advice from your optician.
Protection of nearby personnel
For production welding, a separate, well vented room or enclosed bay is best. In open areas,
surround the operation with low reflective, non- combustible screens or panels. Allow for free air
circulation, particularly at floor level. Provide face shields for all persons who will be looking
directly at the weld. Others working in the area should wear flash goggles. Before starting to
weld, make sure that screen or bay doors are closed.
B) TOXIC FUME PREVENTION
Comply with all precautions in 1B.
C) FIRE AND EXPLOSION PREVENTION
Do not overload arc welding equipment. It may overheat cables and cause a fire. Loose cable
connections may overheat or flash and cause a fire. Never strike an arc on a cylinder or other
pressure vessel. It creates a brittle area that can cause a violent rupture or lead to such a rupture
later under rough handling.
D) SHOCK PREVENTION
Exposed live conductors or other bare metal in the welding circuit, or in unearthed,
electrically-LIVE equipment can fatally shock a person whose body becomes a conductor. DO
NOT STAND, SIT, LIE, LEAN ON, OR TOUCH a wet surface when welding, without suitable
protection.
PROTECTION FOR WEARERS OF ELECTRONIC LIFE SUPPORT DEVICES (PACEMAKERS).
Page 7
7
Magnetic fields from high currents can affect pacemaker operation. Persons wearing
pacemakers should consult with their doctor before going near arc welding or spot welding
operations.
E) PROTECTION AGAINST SHOCK:
Keep body and clothing dry. Never work in damp area without adequate insulation against electric
shock. Stay on a dry duckboard or rubber mat when dampness or sweat can not be avoided.
Sweat, sea water, or moisture between body and an electrically LIVE part - or earthed metal reduces the body surface electrical resistance, enabling dangerous and possibly lethal currents
to flow through the body.
1) Earthing the equipment
When arc welding equipment is earthed according to the National Electrical Code, and the
workpiece is earthed, a voltage may exist between the electrode and any conducting object.
Examples of conducting objects include, but are not limited to, buildings, electrical tools, work
benches, welding power source cases, workpieces, etc. Never touch the electrode and any metal
object unless the welding power source is off. When installing, connect the frames of each unit
such as welding power source, control, work table, and water circulator to the building earth.
Conductors must be adequate to carry earth currents safely. Equipment made electrically LIVE
by stray current may shock, possibly fatally. Do not EARTH to electrical conduit, or to a pipe
carrying ANY gas or a flammable liquid such as oil or fuel.
2) Torch
A fully insulated torch should be used without protruding screws or other damage.
3) Connectors
Fully insulated lock-type connectors should be used to join welding cable.
4) Cables
Frequently inspect cables for wear, cracks and damage. IMMEDIATELY REPLACE those with
excessively worn or damaged insulation to avoid possibly lethal shock from bared cable. Cables
with damaged areas may be taped to give resistance equivalent to original cable. Keep cable dry,
free of oil and grease and protected from hot metal and sparks.
5) Terminals and other exposed parts
Terminals and other exposed parts of electrical units should have insulating covers secured
before operation.
6) Safety devices
Safety devices such as interlocks and circuit breakers should not be disconnected or shunted
out. Before installation, inspection, or service of equipment, shut OFF all power and remove line
fuses (or lock or red-tag switches) to prevent accidental turning ON of power. Do not open power
circuit or change polarity while welding. If, in an emergency, it must be disconnected, guard
against shock burns, or flash from switch arcing. Always shut OFF and disconnect all power to
equipment. A power disconnect switch must be available near the welding power source.
Page 8
8
PREPARATION OF THE WORKING AREA
The working area must be sufficiently spacious, not humid, and well-ventilated as to avoid any
fumes which develop from the welding process and from incidental material adhering to the
pieces to be welded (oils, paints, tars...) which may cause danger to the operator.
Avoid welding tanks which may contain flammable residuals.
DANGER - ELECTRIC SHOCK CAN BE FATAL.
A person qualified in first aid should always be present in the working area.
If person is unconscious and electric shock is suspected, do not touch the
person if he or she is in contact with the welder or cables. Disconnect the
welder from the power source and then use First Aid. Dry wood, or other
insulating material can be used to move cables, if necessary, away from the
person.
ADDITIONAL SAFETY PRECAUTIONS FOR MIG
WELDING
1. ALWAYS ensure that there is full free air circulating around the outer casing of the machine,
and that the louvres are unobstructed.
2. Welding arc can seriously damage your eyes. Both operator and spectators must ALWAYS
use a proper welding face shield or helmet with suitable filter lenses. Proper gloves and
working clothes should be worn at all times.
3. ALWAYS check that the pressure regulator and gauges (where fitted), are working correctly.
DO NOT lubricate the regulator.
4. ALWAYS use the correct regulator. Regulators are designed to be used with a specific
gases.
5. ALWAYS inspect the torch hose before use to ensure it is in good condition.
6. ALWAYS keep the free length of torch hose outside the work area.
7. ALWAYS remove all flammable materials from the welding area.
8. NEVER remove any of the panels unless the machine is disconnected from the supply, AND
never use the machine with any of the panels removed.
9. The MIG welding process uses an INERT gas to protect the weld pool. It isimportant to
ensure the appropriate gas is being used. NEVER use gas from a cylinder, the content of
which is unknown.
NEVER a. Use a damaged cylinder.
b. Lift the cylinder by the valve.
c. Expose the cylinder to a heat source or sparks.
10 NEVER use or store in a damp environment. DO NOT EXPOSE TO RAIN.
Page 9
9
11. ALWAYS keep fire extinguisher handy....’Dry Powder, C02 or BCF, NOT Water
12 NEVER attempt any electrical or mechanical repair unless your are a qualified technician. If
you have a problem with the machine contact your local CLARKE dealer.
13 NEVER continue to weld, if, at any time, you feel even the smallest electric shock.
Stop welding IMMEDIATELY and DO NOT attempt to use the machine until the fault is
diagnosed and corrected.
14 NEVER point the MIG torch at any person or animal.
15 NEVER touch the MIG torch nozzle until the welder is switched OFF and the nozzle has
been allowed to cool.
16 NEVER connect, disconnect, or attempt to service the welding torch, until the machine is
switched OFF and disconnected from the mains supply.
17 NEVER allow the earth cable or torch hose to become wrapped around the operator or any
person in the vicinity.
A comprehensive range of CLARKE safety equipment for use when welding is available from
your local dealer.
ELECTROMAGNETIC INTERFERENCE (EMC)
Whilst this unit complies with EMC regulations, the user is responsible for installing and using the
welding equipment correctly. If electromagnetic disturbance is detected it is the responsibility of
the user to resolve the situation. Remedial action may be as simple as earthing the welding
circuit, see ‘Note’. In other cases it could involve constructing an electromagnetic screen
enclosing the power source and the work complete with associated input filters.
Note :- The welding circuit may or may not be earthed for safety reasons.
Changing the earthing arrangements should only be authorised by a person
who is competent to assess whether the changes will increase the risk of injury,
e.g. by allowing parallel welding current return paths which may damage the
earth circuits of other equipment.
ASSESSMENT OF AREA
Before installing welding equipment the user shall make an assessment of potential
electromagnetic problems in the surrounding area. Avoid using your welder in the vicinity of:
a) other supply cables, control cables, signalling and telephone cables; above, below and
adjacent to the welding equipment;
b) radio and television transmitters and receivers;
c) computer and other control equipment;
d) safety critical equipment, e.g. guarding of industrial equipment;
e) pacemakers and hearing aids etc;
f) equipment used for calibration or measurement;
g) other equipment in the environment. The user shall ensure that other equipment being
used in the environment is compatible. This may require additional protection measures.
Page 10
10
It may be possible to avoid the above by choosing the time of day that welding or other activities
are to be carried out.
The size of the surrounding area to be considered will depend on the structure of the building and
other activities taking place. The surrounding area may extend beyond the boundaries of the
premises.
METHODS OF REDUCING EMISSIONS
Welding equipment will be connected to the mains supply but if interference occurs, it may be
necessary to take additional precautions such as filtering of the mains supply. Consideration
should be given to shielding the supply cable of permanently installed welding equipment, in
metallic conduit or equivalent. Shielding should be electrically continuous throughout its length.
The shielding should be connected to the welding power source so that good electrical contact is
maintained between the conduit and the welding power source enclosure.
The welding equipment should be routinely maintained according to the manufacturer’s
recommendations. All access and service doors and covers should be closed and properly
fastened when the welding equipment is in operation. The welding equipment should not be
modified in any way except for those changes and adjustments covered in the manufacturer’s
instructions. In particular, the spark gaps of arc striking and stabilizing devices should be
adjusted and maintained according to the manufacturers recommendations.
The welding cables should be kept as short as possible and should be positioned close together,
running at or close to the floor level.
Bonding of all metallic components in the welding installation and adjacent to it should be
considered. However, metallic components bonded to the work piece will increase the risk that
the operator could receive a shock by touching these metallic components and the electrodes at
the same time. The operator should be insulated from all such bonded metallic components.
Where the workpiece is not bonded to earth for electrical safety, nor connected to earth because
of its size and position, e.g. ships hull or building steelwork, a connection bonding the workpiece
to earth may reduce emissions in some, but not all instances.
Care should be taken to prevent the earthing of the workpiece increasing the risk of injury to
users, or damage to other electrical equipment.
Where necessary, the connection of the workpiece to earth should be made by a direct
connection to the workpiece, but in some countries where direct connection is not permitted, the
bonding should be achieved by suitable capacitance, selected according to national regulations.
Selective screening and shielding of other cables and equipment in the surrounding area may
alleviate problems of interference. Screening of the entire welding installation may be considered
for special applications.
Page 11
11
ELECTRICAL CONNECTIONS
WARNING! THIS APPLIANCE MUST BE EARTHED.
MIG 220TE & 255TEC
Connect the mains lead, through a suitably fused isolator switch, to a 230 Volt (50Hz) electrical
supply, having a fuse rating in accordance with that given in the specification chart on page 2. A
standard 13 Amp plug MUST NOT be used with this machine.
IMPORTANT: The wires in the mains lead are coloured in accordance with the following
code:
Green & Yellow - Earth
Blue - Neutral
Brown - Live
As the colours of the flexible lead of this appliance may not correspond with the coloured
markings identifying terminals in your electrical supply, proceed as follows:
• Connect GREEN & YELLOW coloured cord to terminal marked with a letter
“E” or Earth symbol “ ” or coloured GREEN or GREEN & YELLOW.
• Connect BROWN cord to terminal marked with a letter “L” or coloured RED.
• Connect BLUE cord to terminal marked with a letter “N” or coloured BLACK.
MIG 270TE
This model is designed for use with a 400V three-phase supply, and should be connected
through a suitably fused isolator switch.
The GREEN or GREEN & YELLOW wire should be connected to the EARTH terminal or terminal
marked with “ ” symbol. The other two wires are for connection to the phase wires.
Cable Extensions:
IMPORTANT:
For extensions up to 10m, the size of the conductors MUST be at least the same size
as that used on the machine - 2.5mm2. It is NOT advised to use extensions greater
than this, but if it is absolutely necessary, the conductor size must be 4mm2 up to a
maximum of 25m in length.
DANGER
NEVER OPERATE THIS MACHINE WITH THE SIDE PANELS PARTIALLY
OPENED OR COMPLETELY REMOVED
Page 12
12
MIG WELDING - PRINCIPLES OF OPERATION
MIG (Metal Inert Gas) welding is a process in which a power wire electrode is fed continuously
into the weld pool at a controlled, constant rate. The wire is connected to the positive side of a
rectified voltage supply. The workpiece is connected to the negative side of the supply. When the
wire is fed, it comes into contact with the workpiece and an arc is struck. The arc melts the wire
and the material, fusing it together. The wire, which is fed by the wire feed motor is fed into the
weld pool, burning itself off at a rate dependent upon the selected wire feed speed. To protect the
weld pool from oxidation and impurities during the welding process, a shielding gas flows over
and around the weld pool. This gas flow must be sufficient to protect the weld, but not be
wasteful.
NOTE:
Poor gas coverage will result in poor welding. Excessive gas coverage is
wasteful and expensive
.
BENEFITS OF MIG WELDING
• 50% faster welding time.
• Operator training time kept to a minimum.
• There is no slag removal, thus eliminating almost all post-welding
cleaning operations.
• Minimum waste of welding consumables.
• Overall, a faster more efficient way of getting the job done.
• Less heat - less distortion.
• Ability to weld thin material.
DECLARATION OF CONFORMITY
We declare that this product complies with the following standards/directives
• 93/68 EEC
• 89/336 EEC
• 73/23 EEC
• 98/37 EC
• EN50 119
• EN 60 974-1
Signed
L.E. Fergusson
Engineering Manager
Page 13
13
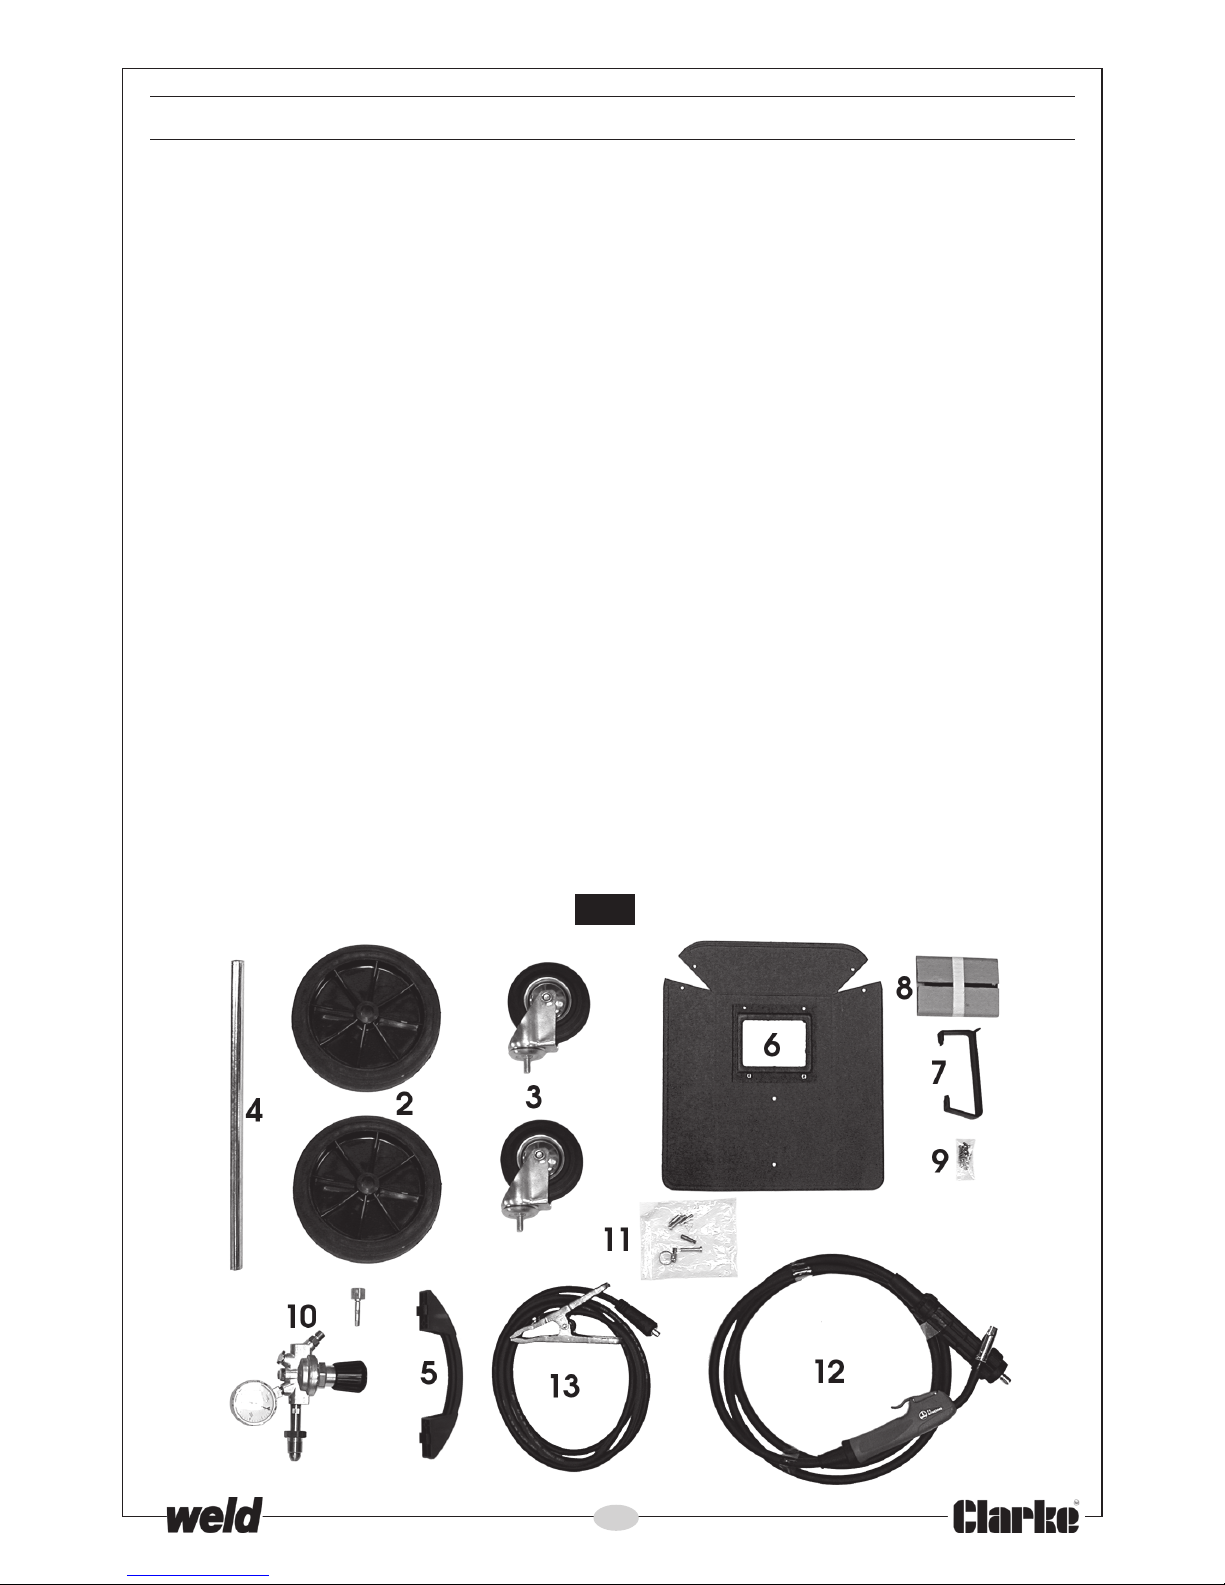
UNPACKING & PARTS IDENTIFICATION
Unpack and lay out the components, checking against the following list. Any damage or
deficiency should be reported to your CLARKE dealer immediately.
Some components are stored within the side compartment. To open the compartment, slide
the recessed handle backwards.
1. Welder complete with power cable and gas hose.
2. 2 x Wheels
3. 2 x Castors
4. 1 x Tubular Axle
5. 1 x Handle
6. 1 x Welding Mask
7. 1 x Welding Mask Handle
8. 1 x Package containing 1x Clear Glass and 1x Dark Glass Lens
9. 1 x Package containing 6 screws and nuts for welding mask
10.1 x Gas Regulator with nut and tail connector.
11.1 x Package containing:
a. 2 x circlips for wheel axle (wheel retainers)
b. 2 x Hex. socket head screws for securing the handle.
c. Worm drive hose clip for gas hose to regulator
d. 3 x spare welding tips...0.6mm and 0.8mm
NOTE: A 0.6mm tip is also fitted to the torch
12. Torch & Hose Assembly
13. Earth Lead Assembly
Fig.1
Page 14
14
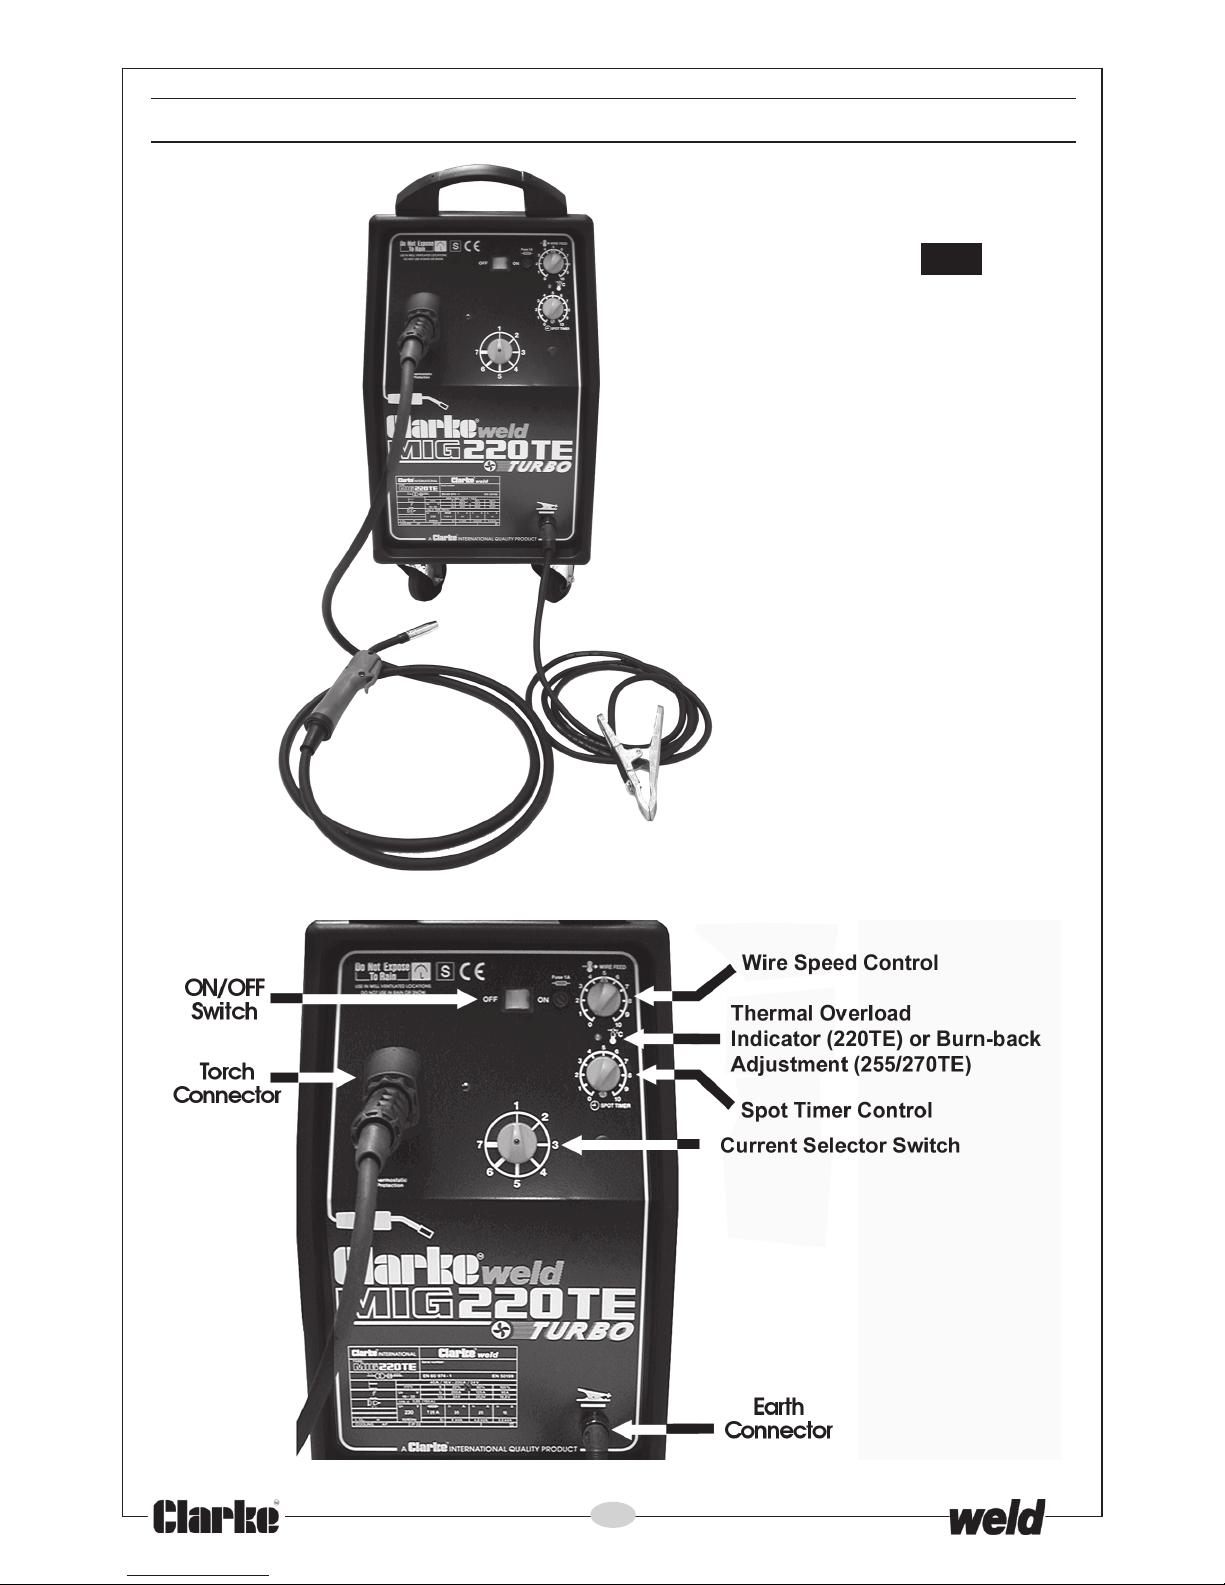
GENERAL LAYOUT
Fig.2
Page 15
15
ASSEMBLY
Wheels & Castors
Raise the machine and thread the axle into its housing and attach the wheels, securing with the
circlips provided.
Thread the castors into their mountings and tighten the bolts.
Handle
Attach the handle to the top front of the machine using the two hex. socket head screws.
Hose and Earth Cable
Simply screw the Torch Hose connector into the adapter on the front panel, ensuring the pins are
correctly aligned. DO NOT force it into place.
Tighten the large plastic round nut.
The earth cable plug is inserted into its receptacle on the lower front panel, ensuring the key lines
up with the keyway, and then rotated through 90 degrees to lock into place.
Gas Supply
It is necessary to obtain a cylinder of gas suitable for the job in hand.
Locate the gas cylinder on the platform at the rear of the unit and secure using the chain
provided.
A regulator is provided, complete with outlet pressure gauge for use with argon or argon mix gas
bottles. Should you wish to use Carbon Dioxide, it will be necessary to purchase an appropriate
regulator with a female connector. Your Clarke dealer will be happy to advise in this regard.
Ensure the outlet of the gas bottle is clean, then screw on the regulator and nip up... do not
overtighten.
Always use the appropriate gas for the material being welded. If you are unsure, consult a
qualified tradesman or a suitable reference book.
Attach the nut and tail to the gas hose using the worm drive clip provided, then screw the nut on
to the regulator outlet and tighten.
Open the gas valve and screw in the regulator knob allow gas into the system to check for gas
leaks. If any are found they must be rectified before proceeding. Turn off the gas when satisfied
the system is leak free.
Page 16
16
All components are now correctly assembled, and the welder
may now be prepared for use as follows:
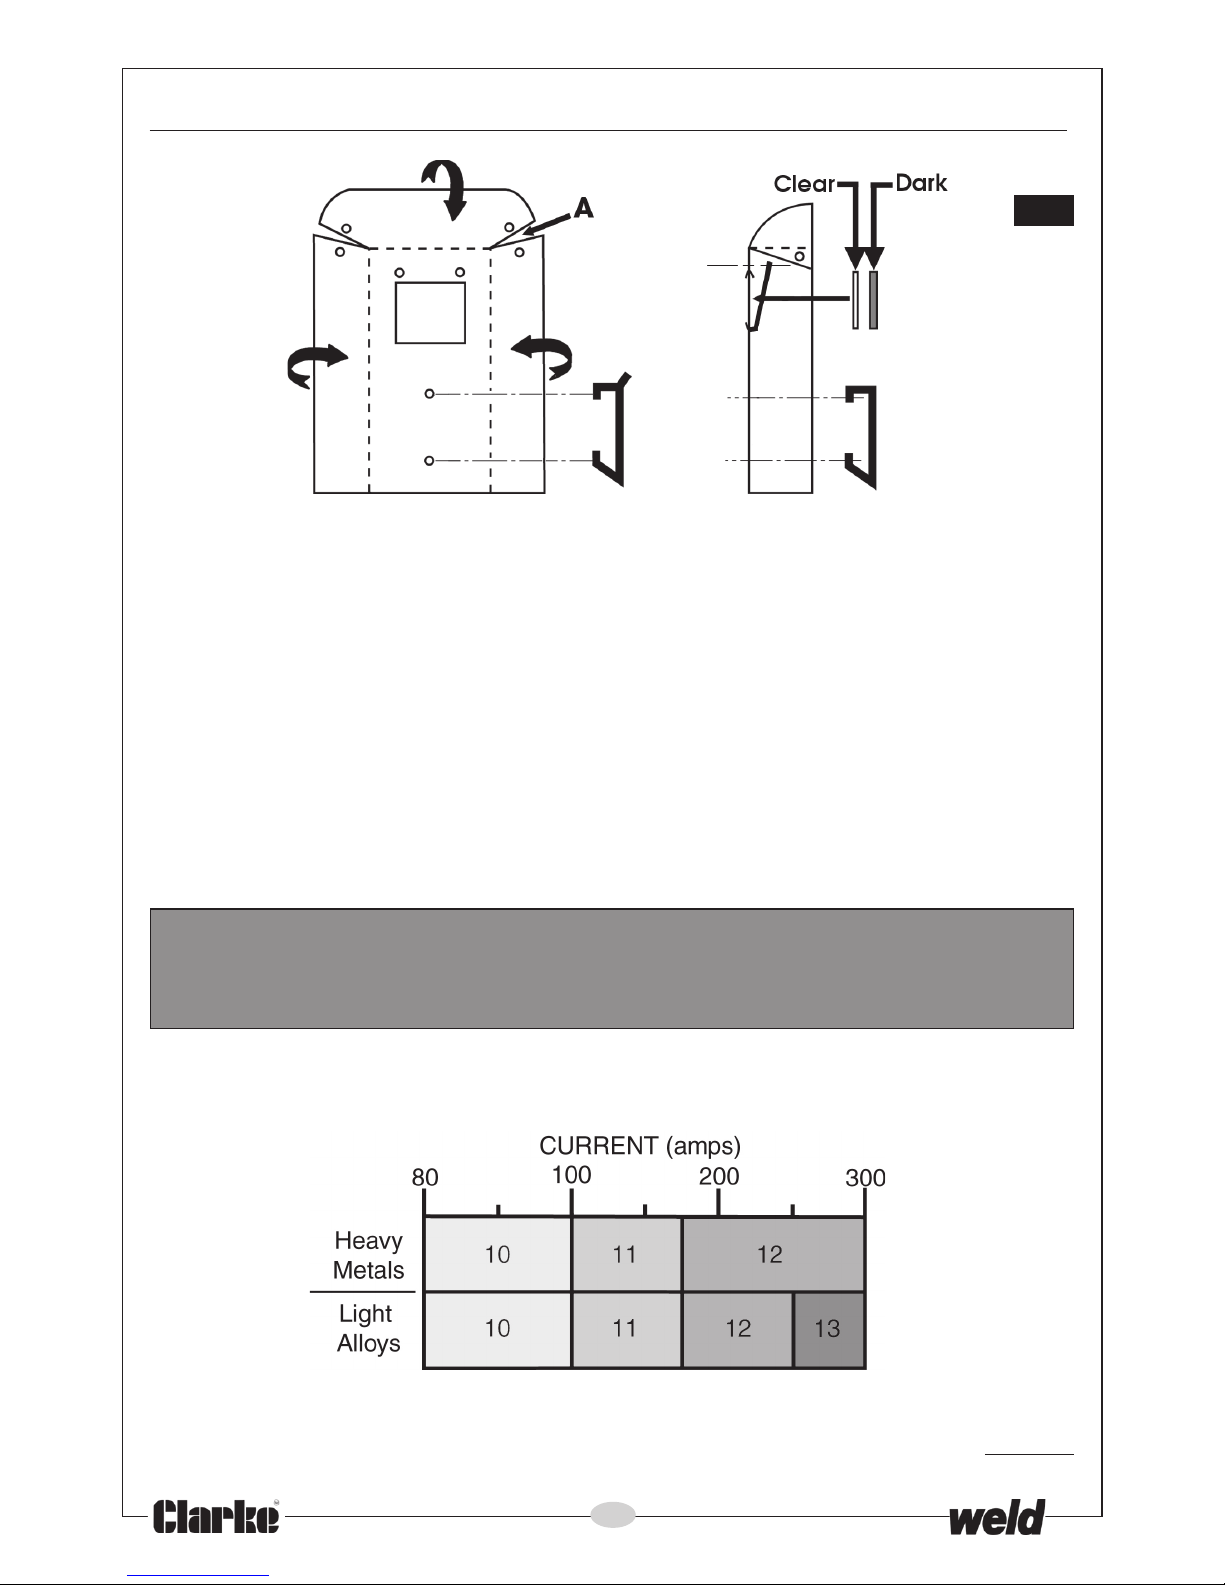
The Welding Shield
1. Remove the shield, handle and screws bag from the packaging.
2. Carefully bend the side and upper panels ‘inwards’ so that the holes in the upper
panel and top of the side panels coincide (A). Secure together with screws and nuts
provided.
3. Prise back the window flap and insert the clear glass first, followed by the dark glass,
ensuring they fit snugly in the recesses, then secure the flap with two screws with nuts
provided.
IMPORTANT: The clear glass MUST installed BEFORE the dark glass.
It is important to pay attention to the notes on welding shield maintenance, given on page 25.
When replacing the glass panels, always use parts supplied by Clarke International. The dark
panel is a certified, specific optical class, and should not be exchanged for any other type.
The clear glass panel should be replaced when it becomes badly pitted.
WARNING:
NEVER look at an electric arc without eye protection as this can injure the
eyes permanently. ALWAYS use a protection mask or welding helmet.
Fig.3
NOTE: The correct shade of glass should be used in accordance with the following
chart:
Page 17
17
Installing the Welding Wire
NOTE: These machines are designed to accept either the Clarke 5kg or 15kg wire
spools of mild steel, stainless steel or aluminium according to the type of metal you
wish to weld. Wire spools must be purchased separately. See your Clarke dealer for
full details.
1. IMPORTANT: Ensure that the gas and electrical supplies are disconnected.
PREPARATION FOR USE
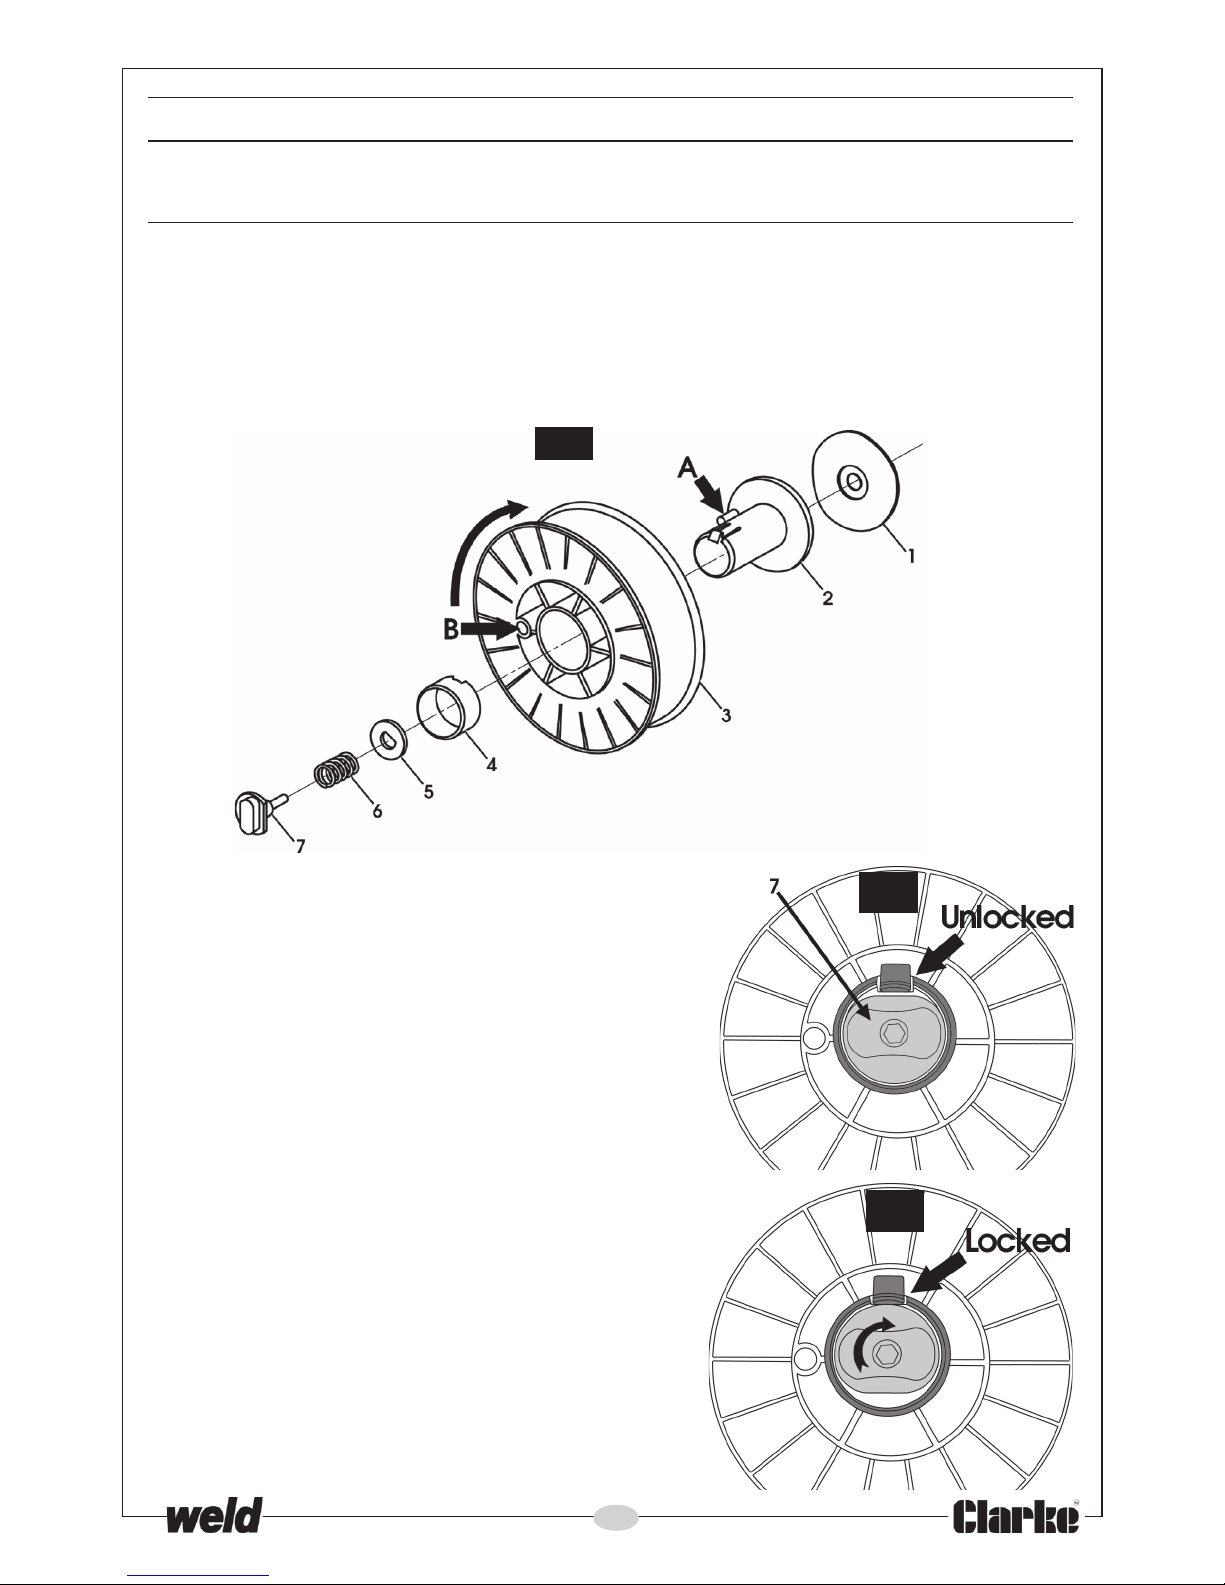
2. To fit the wire spool shown
in Fig 4, firstly open the
side compartment by
pulling the recessed catch
backwards.
Fig.6
3. Turn the plastic knob with cam (7) to the position
shown in Fig 5, so that the latch is unlocked, and
pull off the collar (6).
4. Slide the spool on to the shaft, ensuring that the
Peg ‘A’ locates snugly in locating hole ‘B’,
ensuring the direction of feed of the wire is in the
direction of the arrow.
5. Replace the collar - 4, (5kg spool ONLY), and turn
the plastic knob with the cam (7) to the position
shown in Fig 6, thereby locking the spool on the
shaft.
NOTE: The plastic knob, (item 7 - Fig 4), is also
used to apply slight tension to the wire spool.
This prevents the spool from running freely,
which could cause the wire to unspool,
creating a ‘birds nest’ tangle within the side
compartment. Adjust by hand and test the
tension.
1. Pressure plate
2. Mounting Shaft
3. Wire Spool
4. Collar
5. Flat Washer
6. Spring
7. Plastic Nut
Fig.5
Fig.4
Page 18
18
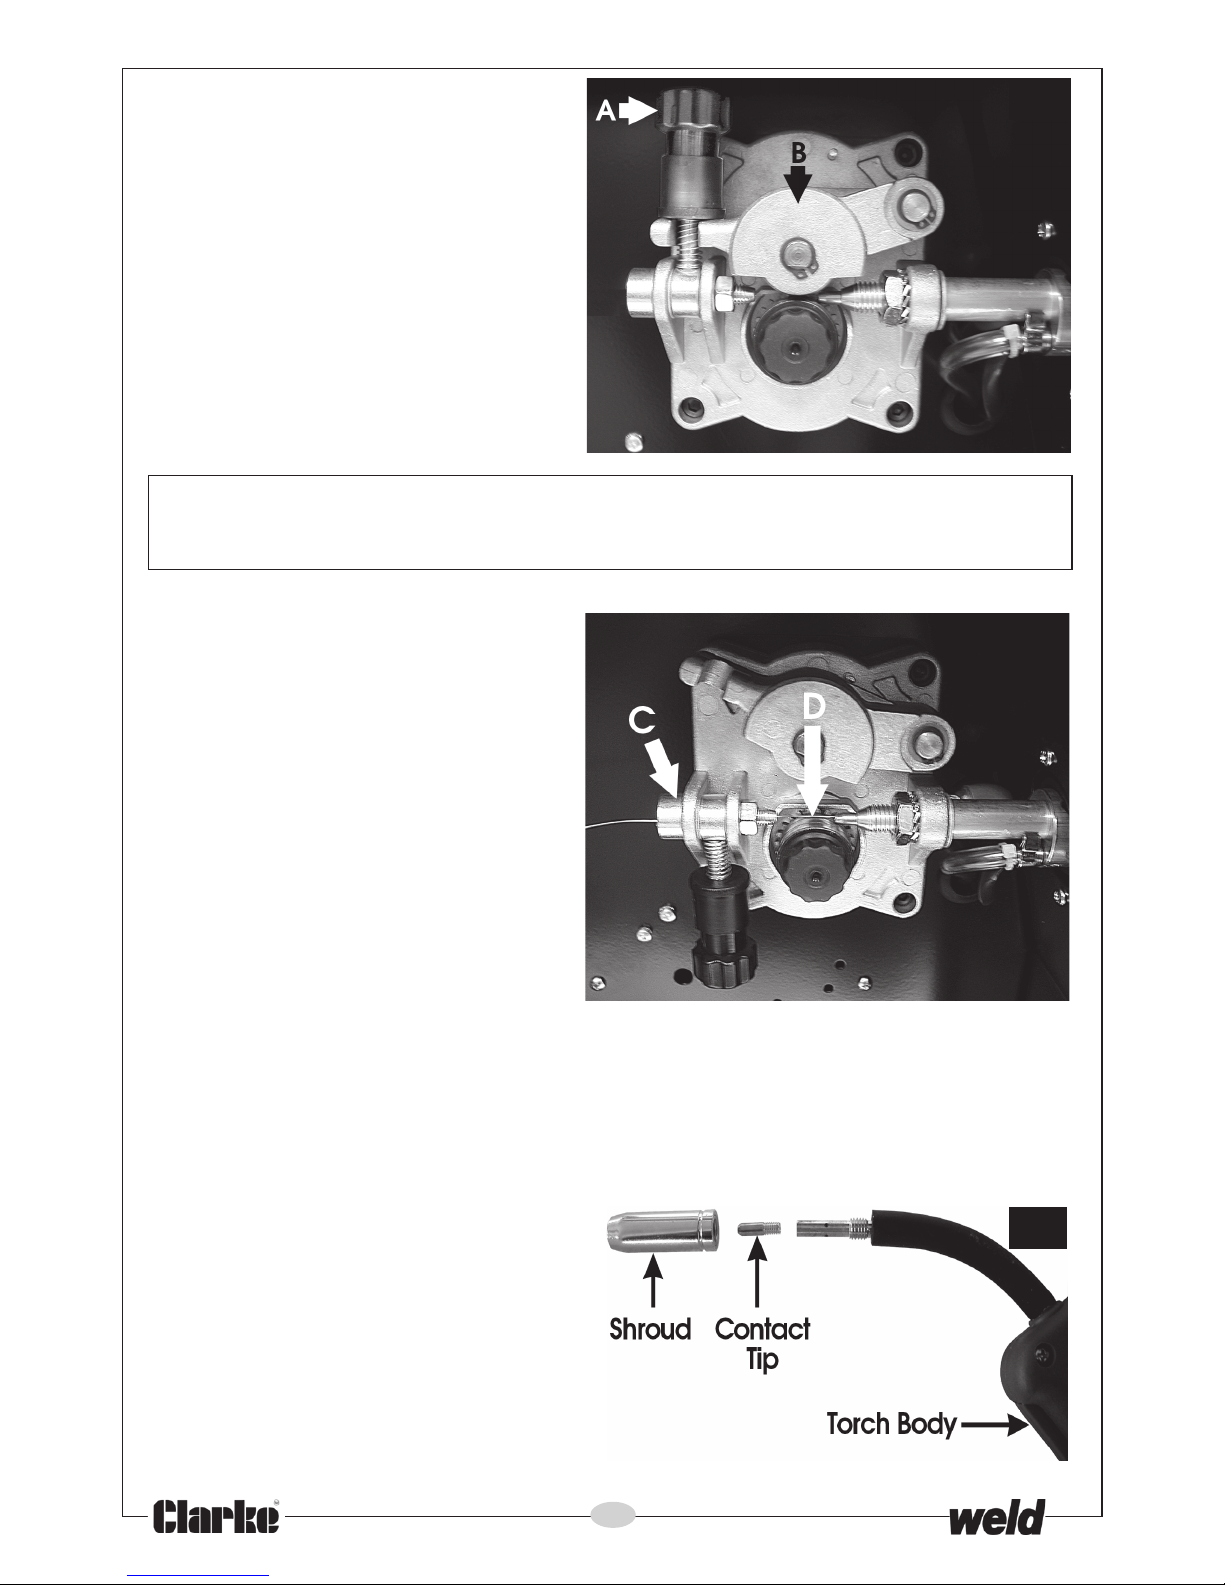
6. Unscrew the pressure roller bracket
securing knob (A, in Fig 7), whilst
holding down the pressure roller
bracket (B), against spring pressure,
so that the screw rod hinges out of its
slot. This releases the pressure roller
bracket which, when released,
will pivot upwards under spring
pressure.
IMPORTANT!
Before fitting any wire, ensure the correct groove on the roller is in place.
(See page 19).
Fig.9
7. Pull out the end of the wire
from the rim of the spool, taking
care NOT to release it. The spool is
wound firmly and should remain this
way.
Ensuring the wire is straight and not
kinked in any way, clip off the end
with a sharp pair of snips ensuring
there are no burrs or sharp edges.
Proceed to feed it through the guide
tube (C, Fig 8), over the groove on
the roller (D), and into the wire liner,
by about 10 - 15 cm.
8. Reposition the pressure roller
bracket and securing knob (A) and
tighten slightly.
Tightening the knob (A) too tightly will crush the wire and damage the
wire feed motor, too loose will not allow the wire to be pulled by the roller.
9. (Ref. Fig 9)
Remove the torch shroud by twisting it
anti clockwise and pulling it off, then
unscrew the contact tip.
Should any wire protrude from the
tip....pull it out completely and discard.
Fig.7
Fig.8
Page 19
19
10. Close the side panel of the machine and switch on at the mains or isolator.
11. Set the wire feed rotary switch on the front panel to position 6 or 7, switch on the machine
and press the trigger.
The wire will feed through the hose and when it appears at the torch end, release the trigger,
switch off the machine and disconnect from the mains supply. Replace the contact tip and
the torch shroud.
IMPORTANT:
Ensure the hose is kept straight during this operation, to assist the wire as it is
fed through to the wire liner and torch.
Selecting the Correct Drive Roller Groove
As previously mentioned, it is important that the correct groove in the drive roller is selected for
the particular wire being used. The roller provided has 0.6 and 0.88mm grooves.
The welder is factory set with the 0.8mm groove in position.
To change grooves, proceed as follows:
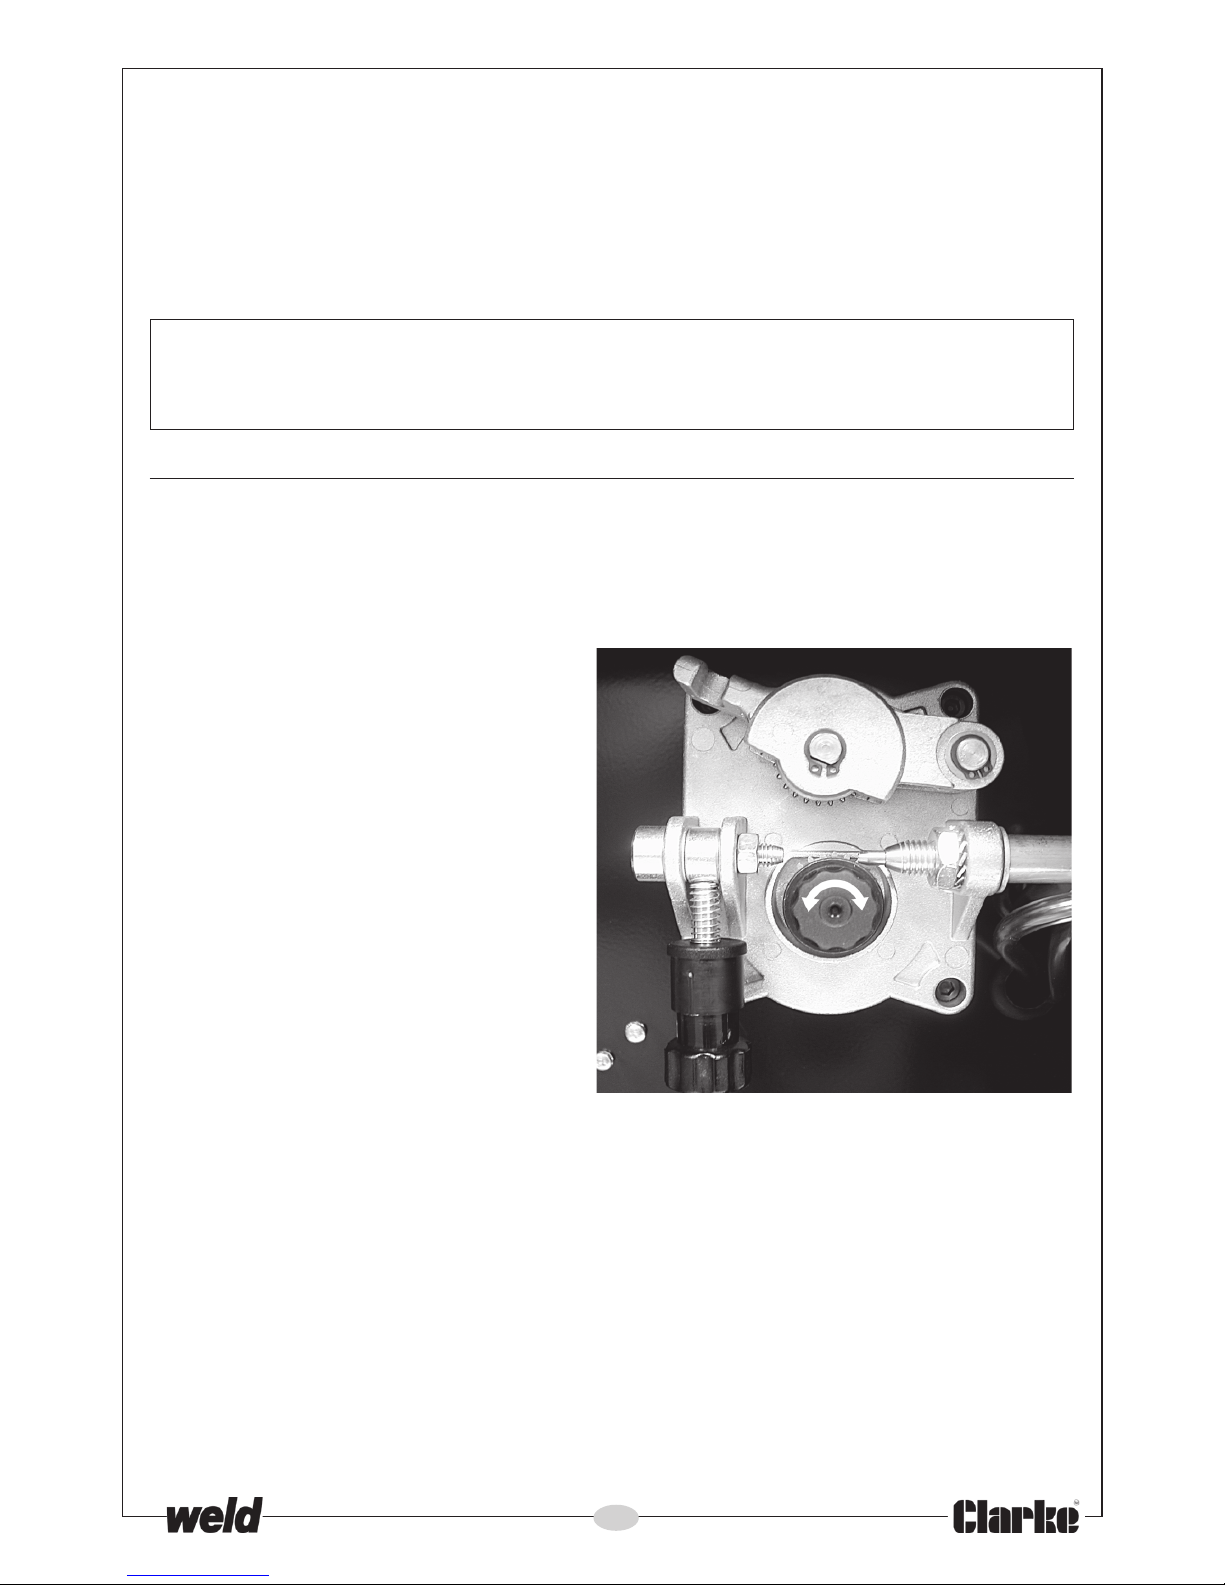
1. With the pressure roller bracket raised,
and the old wire removed, remove the
roller securing knob (arrowed), by
turning it fully anti-clockwise, then pull
the roller from the shaft.
2. Ensure the appropriate groove is facing
inwards before sliding the roller on to the
shaft.
Screw on the securing knob to lock the
roller securely in place.
Fig.10
Page 20
20
OPERATION
Each time you use the machine it will be necessary to perform the following operations:
Check the Welding Wire
Check to ensure the correct type of welding wire is installed for the job in hand and is correctly
adjusted.
Prepare the Work
MOST IMPORTANT!
It is vital that the workpiece is perfectly clean at the point of weld. Any coating, plating or
corrosion MUST be removed, otherwise a good weld will be impossible to achieve.
Set the Controls
In order to produce a satisfactory weld, the controls must be fine tuned whenever there is a
material change in weld characteristics. This is generally referred to as ‘Tuning the Welder’.
The tuning of a MIG welding machine requires some practice, due to the fact that - contrary to
the arc welding procedure - two parameters must be accommodated to achieve a perfect weld.
These are:
(1) Welding Current, and (2) Wire Feed Speed,
It is important to arrive at the correct combination to suit the type and thickness of material to be
welded.
The current, necessary for welding, is directly related to the wire feed speed.
As the current is increased, the wire feed speed is also increased.
Conversely, if current is decreased the wire feed speed is decreased.
A change in wire diameter results in changed parameters. A smaller diameter wire requires an
increase in wire feed speed to reach the same current.
If certain limits are exceeded, a satisfactory weld cannot be obtained. These are:
A) An excessive wire feed speed (too high with regard to the welding current), results in pulsing
within the torch. This is because the wire electrode dips into the puddle and cannot be
melted off fast enough.
B) If the welding current is set too high, large drops can be seen at the end of the wire
electrode. These drops are often deposited beside the welding seam.
The correct rate of wire feed speed and welding current, results in very little spatter and a
continuous, intensive hissing can be heard from the arc.
Page 21
21
(i) WELDING CURRENT CONTROL
Select the welding current according to the type of metal and thickness to be welded. The control
has 7 positions as indicated in the chart below. Experience will determine the optimum setting for
the job in hand, but the chart gives general settings from which to work.
PLEASE NOTE: If the current and hence the wire speed is increased, the volume of
gas at the nozzle must also be increased. Turn the regulator knob accordingly.
(ii) WIRE FEED SPEED CONTROL
The WIRE FEED Rotary Control Knob, with graduations from 0 to 10, is used to fine tune the
wire speed feed to the nozzle. The knob should be set to position 6 to begin with for welding
steel, and 8 for welding aluminium, then adjusted as required.
Note: This control is for fine tuning the wire speed. The speed of wire delivery will
increase automatically as the current is increased and vice versa. Therefore,
once the ideal speed is achieved by fine tuning, it should not be necessary to
adjust this control when the welding current is changed.
It is always better to start with too high a speed, and back off slightly, to avoid
the possibility of the wire welding itself to the tip.
Timer Control
This is explained in more detail on page 23. For all normal welding operations, set this control to
zero.
Welding Wire
Trim the welding wire so that it protrudes no more than 5mm from the end of the shroud.
1 0.6 LOW
2 0.6 LOW
3 0.6 - 0.8 MEDIUM
4 0.6 - 0.8 MEDIUM
5 0.8 MEDIUM _ HIGH
6 0.8 HIGH
7 1.0 HIGH
Steel Wire
Diameter
(mm)
Wire Speed
Adjustment
Switch
Positions
3
4
5
1
2
6
7
Page 22
22
The Earth Clamp
Attach the earth clamp to the workpiece as close to the point of weld as possible, without it being
intrusive. Ensure there is good contact and if necessary, clean the area with a wire brush
beforehand.... Remember, the contact MUST be on bare metal - thoroughly clean.
The Gas Valve
Open the gas valve on the gas cylinder. Regulate the pressure by turning the regulator knob
clockwise (to increase pressure), and adjust to the desired setting. NOTE: this varies with
different metals, thicknesses and currents. Refer to a MIG welding manual for instructions.
Your welder is now fully prepared for welding as follows:
With the welding current set, and welding wire trimmed, set the wire feed control to 6, (8 for
aluminium).
Plug the machine into the mains supply or switch on at the isolator and ensuring all precautions
have been taken and with the machine set up correctly, switch ON the machine and lower the
torch to the workpiece with one hand, whilst holding the welding mask in the other.
Approach the work with the tip at an angle of approx. 45O and pull the torch trigger fully. A welding
current is now available at the tip and gas will be issued.
As the wire touches the workpiece, an arc will be struck......BEFORE it is struck, cover the face
with the face mask.
Maintain a gap of approx. 5 - 7mm from the workpiece to the tip, and feed the wire into the
molten pool at a steady rate, along the line of the proposed weld.
The speed of weld will depend upon the wire speed and welding current.
NOTES:
As MIG welding is an acquired skill, it is strongly advised that, if you are not fully
familiar with this type of welding, you practice on a piece of material with the
same characteristics as your workpiece, until you are satisfied with the result,
and you have fine tuned your welder to produce a satisfactory weld.
One of the problems experienced with novice welders, is the welding wire
sticking to the contact tip. This is as a result of the wire feed speed being too
slow. It is always better therefore to start with too high a speed, and back off
slightly, to avoid the possibility of the wire welding itself to the tip. This is the
reason position 6 is recommended for start up.
The Wire Feed control is for fine tuning the wire speed. The speed of wire
delivery will increase automatically as the current is increased from MIN to
MAX, and vice versa. Therefore, once the ideal speed is achieved, by fine
tuning, it should not be necessary to adjust this control when the welding
current is changed.
Listen to the sound made. An irregular crackling sound denotes too high a wire
speed. Decrease the speed until a regular, strong buzzing sound is heard.
Page 23
23
Thermal Overload (MIG220TE)
The ‘Thermal Overload’ is a safety device which shuts off the welder when the duty cycle has
been exceeded. This is to prevent damage to the machine caused by overheating.
When this occurs, the warning lamp will glow (amber). Allow the welder to cool, until the amber
light extinguishes before resuming.
For details of the duty cycle...i.e. the length of time the machine may be used at a particular
welding current, refer to the data and notes on page 24.
Burn Back Adjustment
This takes the form of a trimmer, located between the control knobs on the front panel which can
be adjusted with a screwdriver eitther clockwise or anti-clockwise.
It is used to regulate the amount of welding wire to “burn back” after releasing the trigger of the
torch. For example, if this is set to Maximum, when the weld is finished, the wire will burn back
almost to the nozzle tip. Initially set the trimmer to an intermediate setting but this may be
adjusted according to the diameter of wire being used.
GENERAL INFORMATION
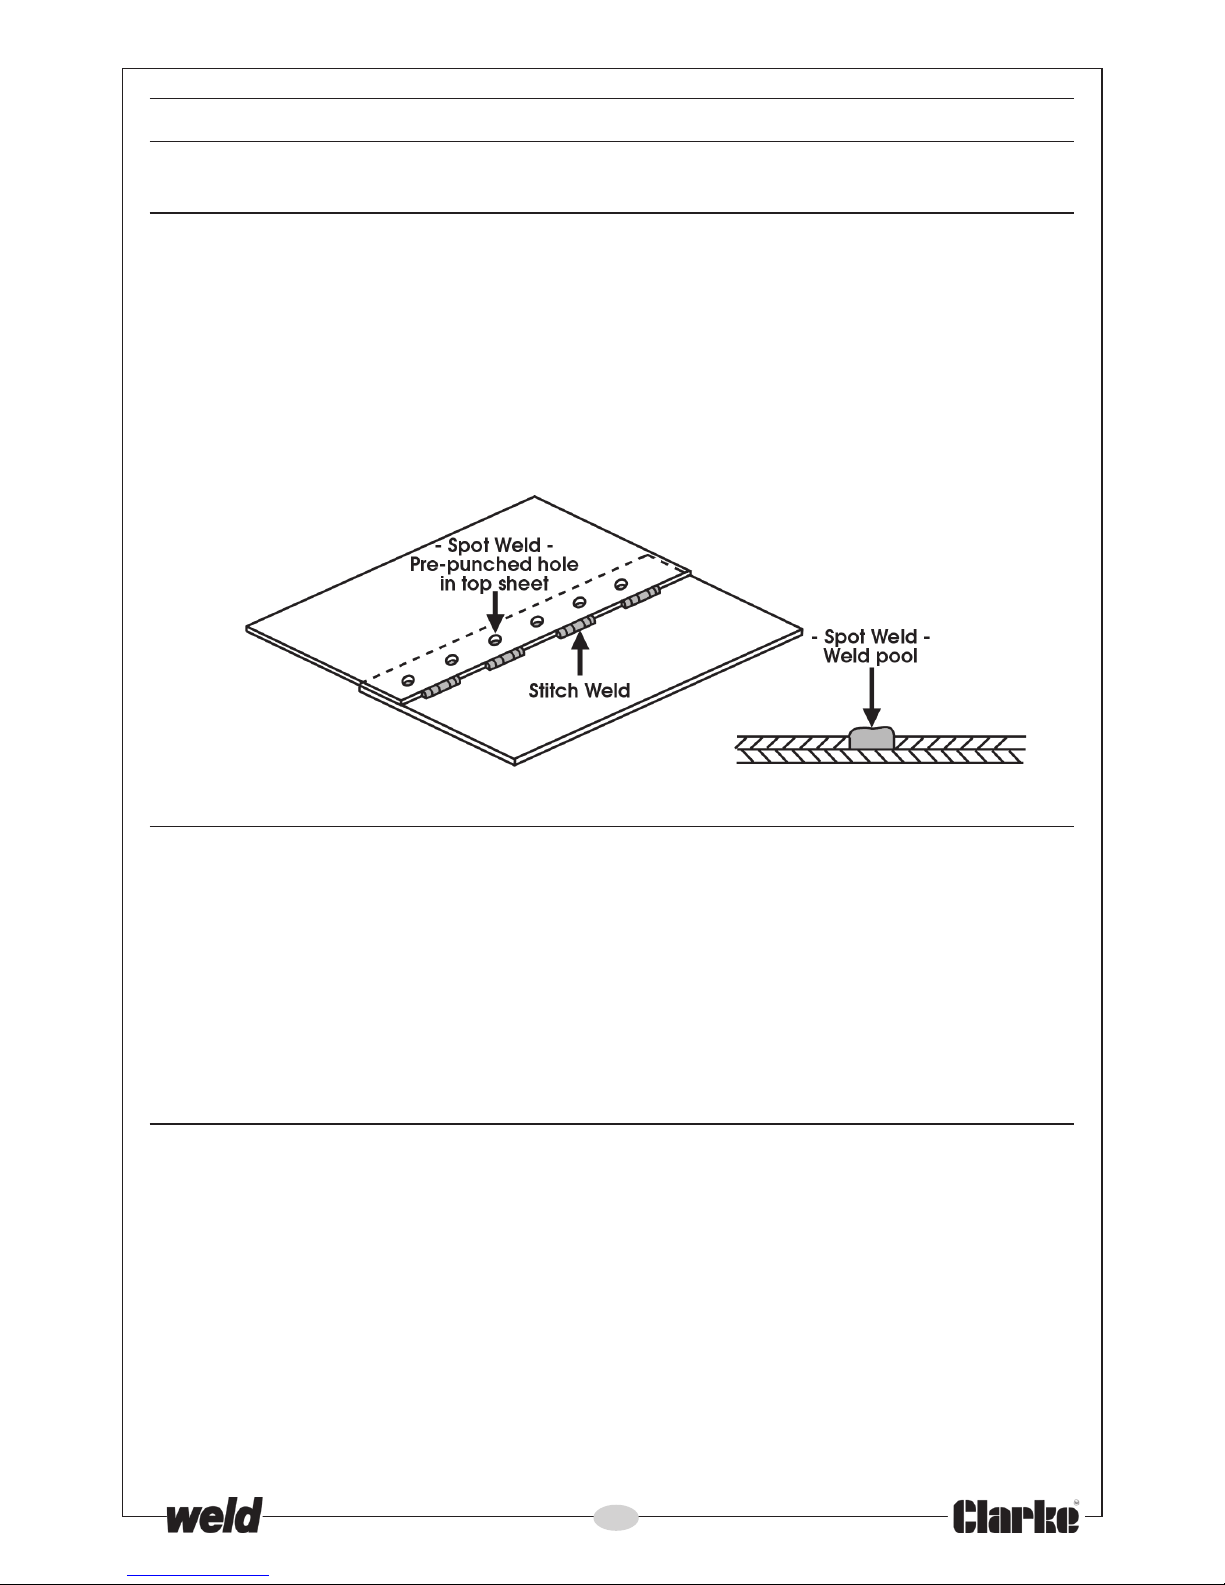
Spot Timer Control
This control may be used for spot (plug) welding, or stitch welding. The control is set so that the
duration of weld lasts for a predetermined time.
For plug welding, a special nozzle is required, (see your CLARKE dealer) which is pressed hard
against the two pieces of material to be welded, as the trigger is pressed. The arc will last for a
predetermined time, depending upon the control setting, melting the metal and fusing the two
parts together.
Allow a short period with parts held together before withdrawing the nozzle.
Page 24
24
WELDING TIPS
• Try to maintain the tip of the nozzle at an angle of approx. 45O and at a constant distance
of approx 5-7mm from the workpiece.
• Try to maintain a constant speed of movement with the torch.
• Do not weld in windy conditions or in an area where ventilation is a problem, or where air
flow fluctuates.
• ALWAYS keep the wire and nozzle clean...NEVER use rusted wire.
• Avoid sharp bends or kinks in the welding hose.
• Whenever possible, clean out the wire liner with compressed air when replacing the wire
spool.
• Periodically remove the dust, using LOW PRESSURE compressed air, within the casing.
Adequate heat dissipation is essential during the welders operation.
DUTY CYCLE
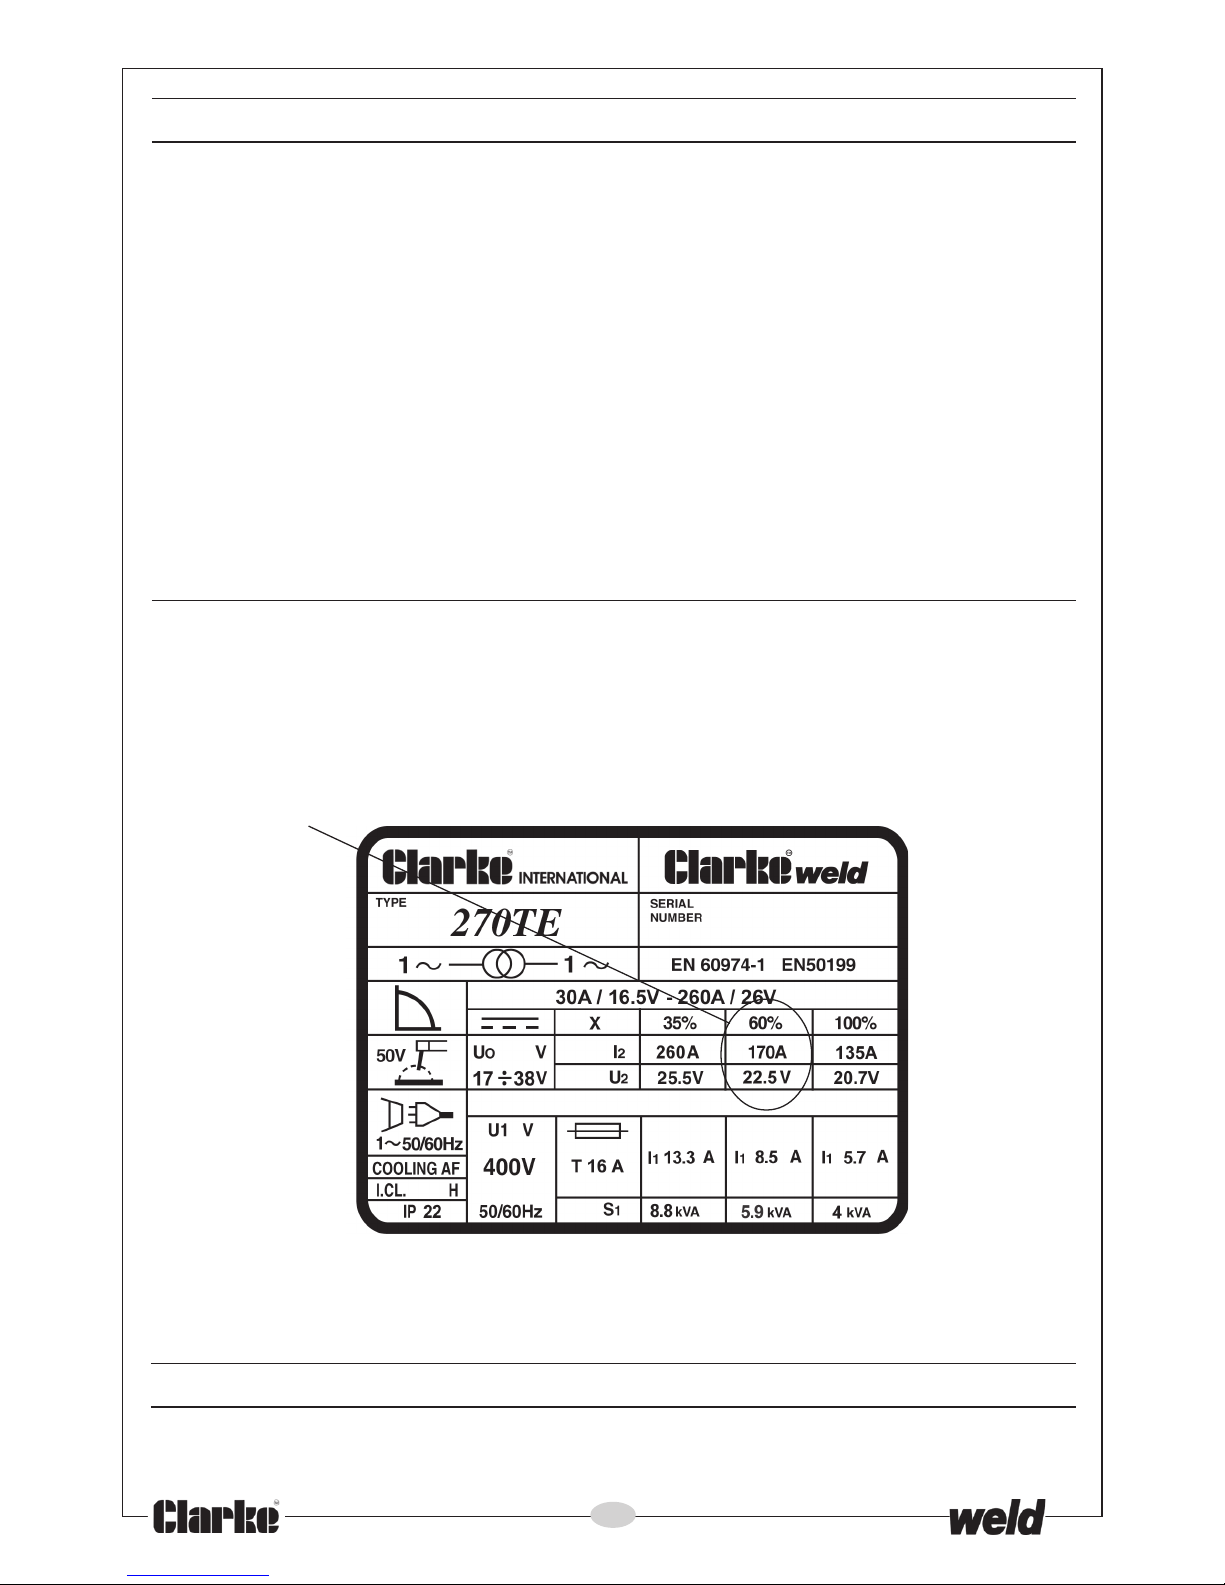
These models are covered by regulations EN 60974-1 and EN 50199, where the Duty Cycle
(X) is expressed as a percentage of time the machine may be used in a given period for a
specified welding current.
i.e. using the example below, which is an illustration of the 270TE data plate.....
When welding at 170 Amps the machine may be used for 6 minutes (60%) in any 10 minute
period..........
............or, the machine may be used continuously, (100%) when welding at 135 Amps
ACCESSORIES
A full range of accessories is available from your Clarke dealer.
Page 25
25
MAINTENANCE
WARNING!
ELECTRICITY CAN KILL....NEVER TOUCH LIVE ELECTRICAL COMPONENTS
DISCONNECT THE POWER SUPPLY BEFORE ALL INSPECTIONS AND MAINTENANCE
OPERATIONS
BEWARE HOT SURFACES.....ALWAYS LET THE POWER SUPPLY COOL DOWN BEFORE
ACCESSING INTERNAL COMPONENTS.
Frequency of maintenance operations depends on the operating conditions, how intensively the
welder is used, and how clean or dirty the welding site is (aggressive atmospheres, etc).
Always inspect the earth return and torch hose, before use to ensure they are in perfect condition
and earth clamp is clean and secured correctly to the cable.
Check the gas hose and pressure regulator for security and serviceability, and ensure there is
sufficient gas to complete the job in hand.
As a general rule the power supply should be inspected internally at least annually. Consult your
CLARKE dealer.
THE WELDING SHIELD
Always maintain the welding shield in good condition. If the clear glass protection lens becomes
badly pitted, sufficient to interfere with vision, or cracked, have it replaced immediately.
Replacement clear and dark lenses are available from your Clarke dealer - see Parts Lists for
details. NEVER use any dark filter lens other than that provided by CLARKE International, or one
with the same certified ‘Optical class’ (degree of protection).
The shield should always be cleaned with a clean soft cloth after use, ensuring the lenses are
clean. Remove any dust that may have accumulated and store it in a safe place where it cannot
be damaged. NEVER use a shield that is not in perfect condition.
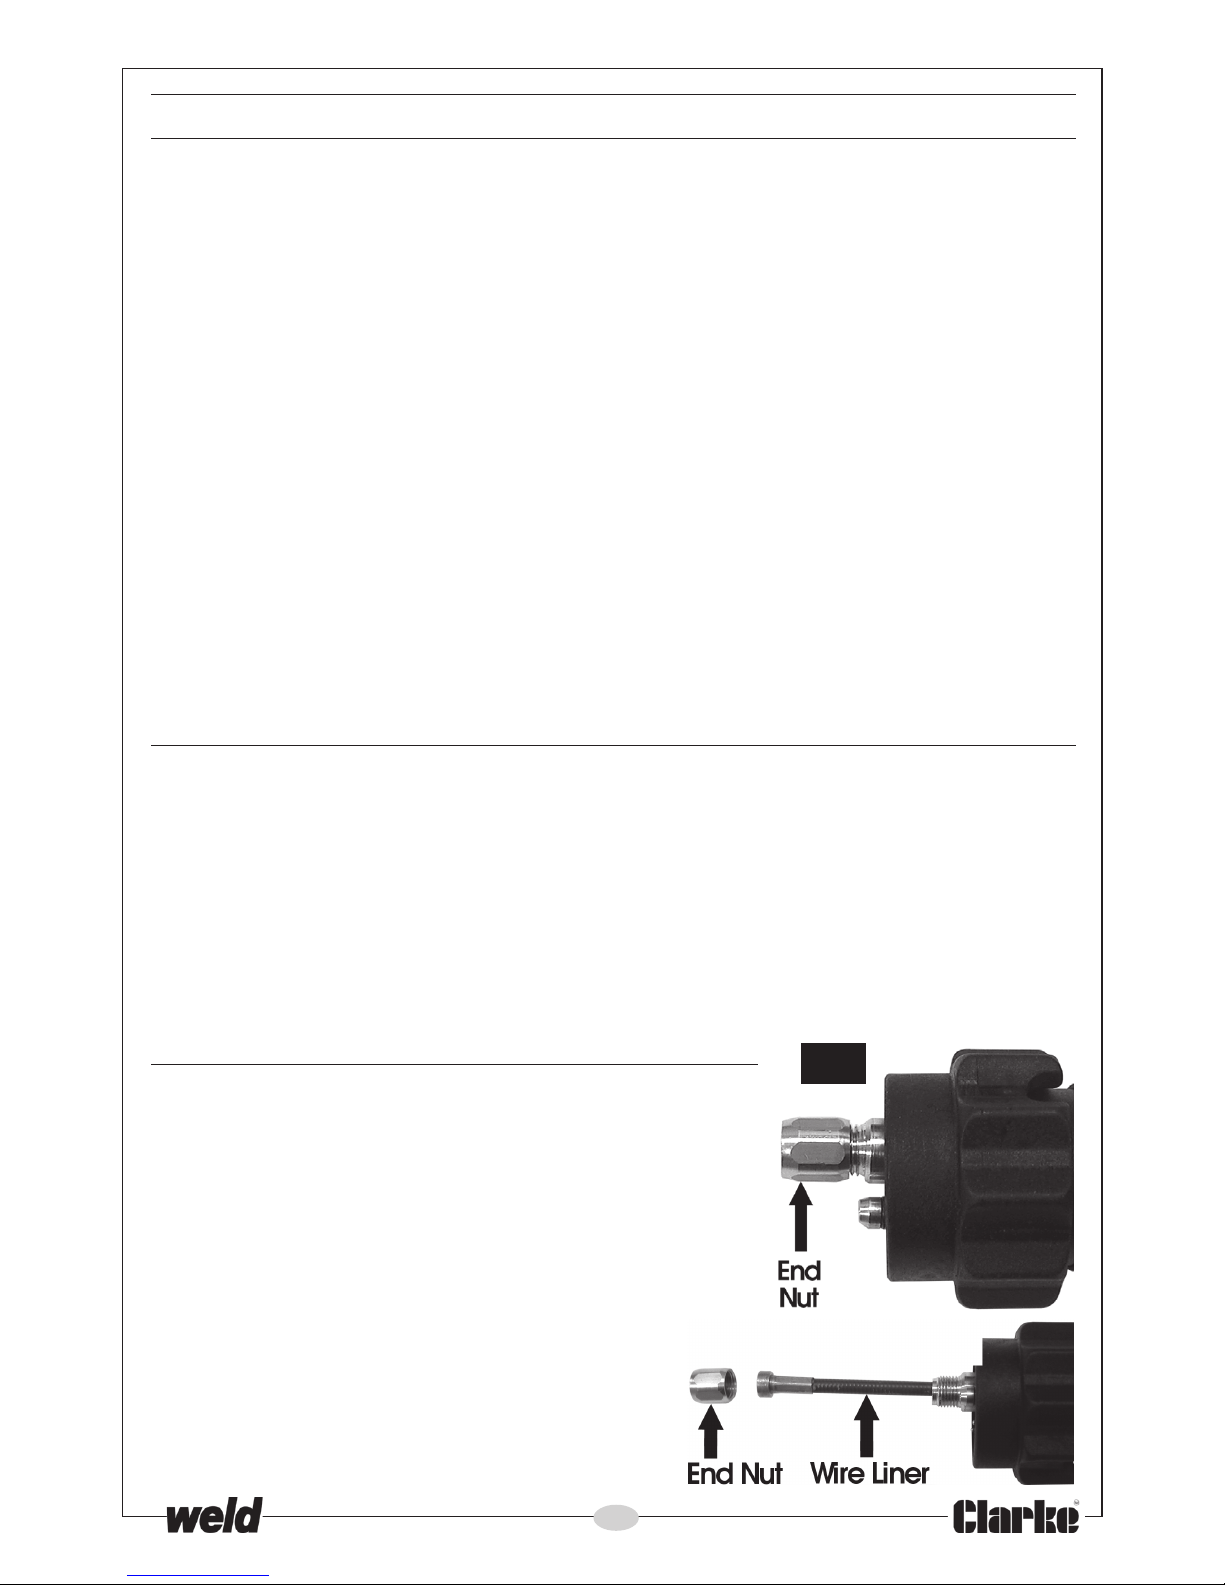
RENEWING THE WIRE LINER
If the liner becomes damaged or kinked it will be necessary to
replace it.
1. Remove the welding wire from the hose & torch assembly,
either by cutting it at the wire spool and pulling through
from the nozzle end, or rewinding it back on the spool.
2. Disconnect the hose from the machine.
3. Unscrew the end not shown in Fig 11 using a
12mm spanner and having straightened the hose
assembly, pull the liner completely out of the
hose.
4. Thread the new liner into the hose fully, then
screw the end nut back into place.
Fig.11
Page 26

26
Your Clarke Mig Welder has been designed to give long and trouble free service. If, however,
having followed the instructions in this booklet carefully, you still encounter problems, the
following points should help identify and resolve them.
PROBLEM CAUSE REMEDY
1. No “life” from welder a) Check fuses and mains lead a) Replace fuses as necessary If
problem persists return welder to
your local dealer
b) Check fuse size
2. No wire feed Motor malfunction Return welder to your local dealer
3. Feed motor operates a) Insufficient Feed Roller Pressure a) Increase roller pressure
but wire will not feed b) Burr on end of wire b) Re-cut wire square with no burr
c) Liner blocked or damaged c) Clean with compressed air or
replace liner.
d) Inferior wire d) Use only good “clean” wire
e) Roller worn out e) Replace roller
4. Wire welds itself to tip a) Wire feed speed too low a) Unscrew tip, cut wire and fit new tip
Increase wire speed before
operating again
b) Wrong size tip b) Fit correct size tip
5. Wire feeds into ‘birds a) Wire welded to tip a) As above plus reduce feed roller
nest’ tangle pressure so that if blockage occurs
wire slips on roller i.e. no feed
b) Wire liner damaged preventing b) Renew wire liner
smooth operation
6. Loose coils of wire Drum brake too slack Tighten drum brake
tangle around wire Caution: Do not over-tighten
drum inside machine
7. Erratic wire feed a) Drum brake too tight a) Loosen drum brake slightly
b) Feed roller worn b) Check and replace if necessary
c) Insufficient pressure on feed roller c) Increase pressure on feed roller
Caution: Do not over-tighten
d) Wire dirty, rusty, damp or bent d) Re-cut wire and ensure it is clean
e) Liner partially blocked e) Clean with compressed air
8. Poor quality welds a) Insufficient gas at weld area a) Check that gas is not being blown
away by draughts and if so move
to more sheltered weld area. If not
increase gas supply
b) Incorrect gas/wire combination b) Consult your MIG welding manual
for correct set-up
c) Rusty, painted, damp, oil or c) Ensure workpiece is clean and dry
greasy workpiece
d) Rusty/dirty wire d) Ensure wire is clean and dry
e) Poor earth contact e) Check earth clamp/work onnection.
9. Wire jams in tip when a) Tip too small a) Use slightly oversize tip ie., for 0.8mm
welding aluminium wire use 1mm tip. (Note: Applies to
aluminium only)
10. Welder cuts out a) Duty cycle exceeded a) Allow welder to cool 15-30 mins
whilst in use (auto cut-out operates) before continuing
Note: If duty cycle is continually
exceeded, damage to the welder
may result, and welder output is
probably too small for application.
If you have any problems which cannot be resolved by reference to the above, or if you
TROUBLESHOOTING
Page 27
27
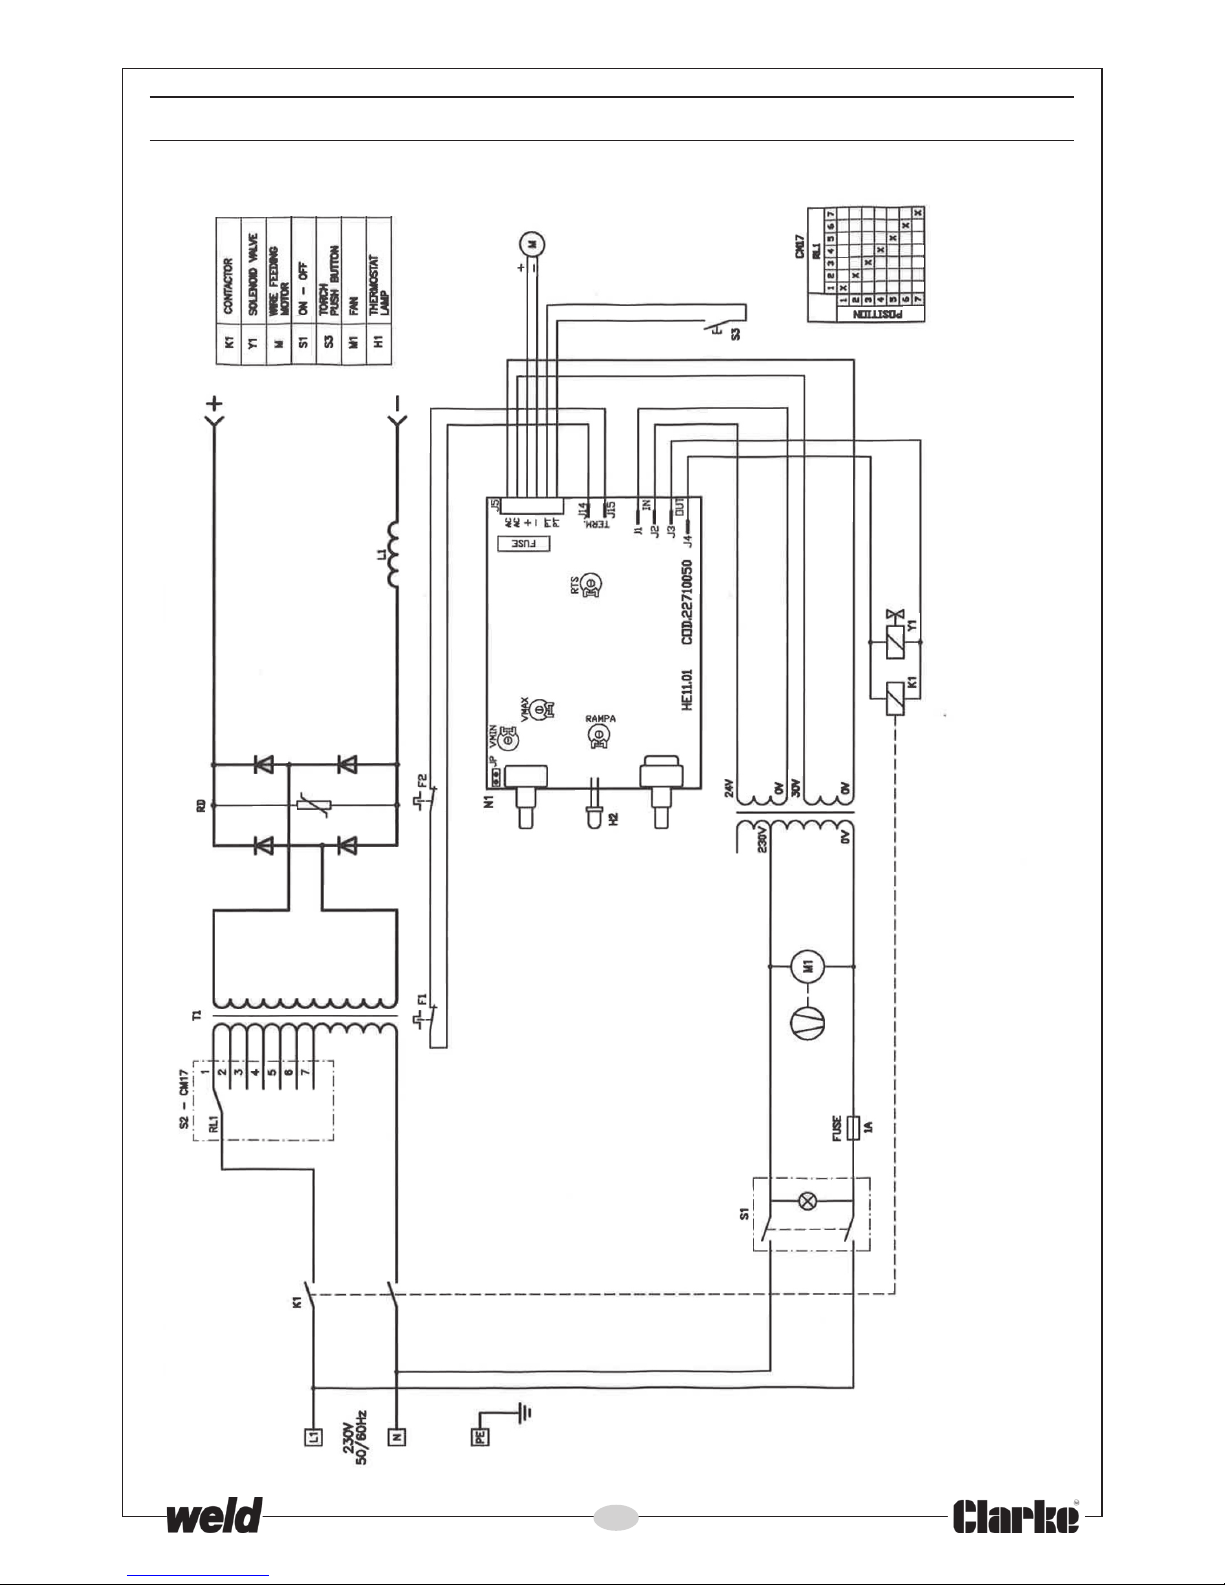
WIRING DIAGRAM - MIG220TE
Page 28
28
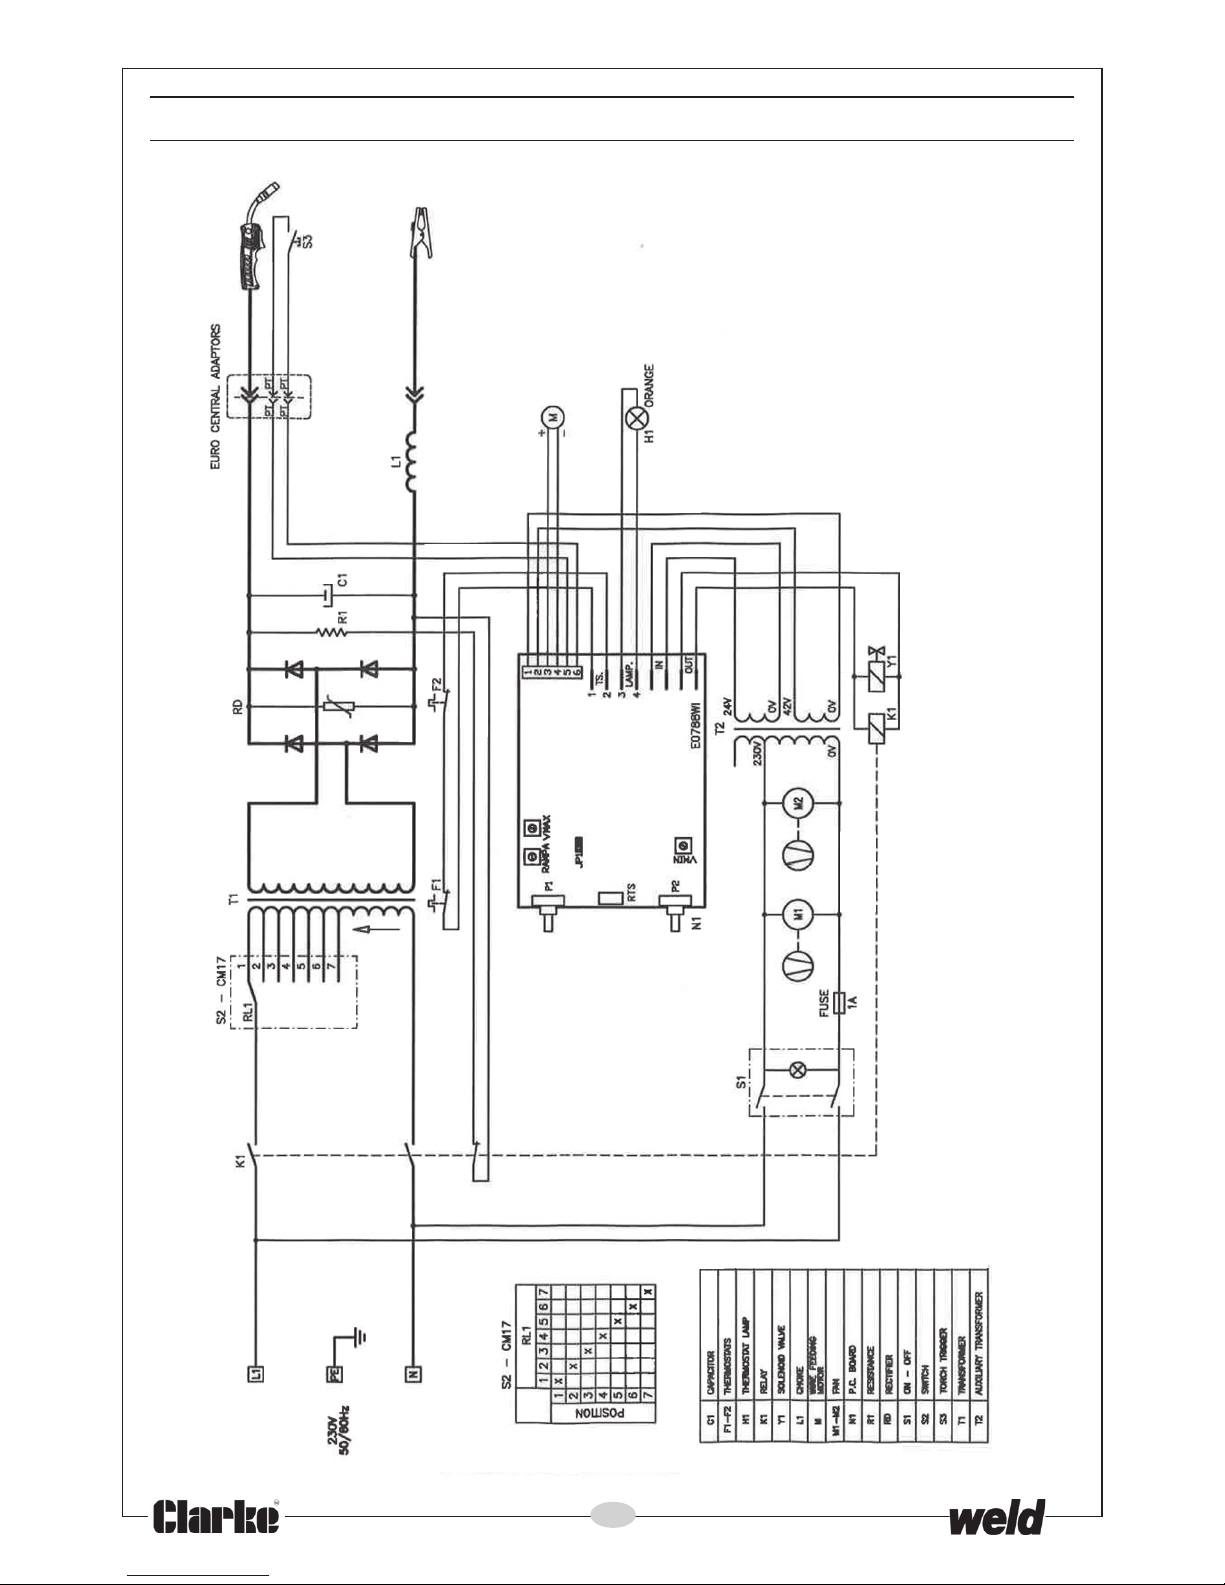
WIRING DIAGRAM - MIG255TEC
Page 29

29
WIRING DIAGRAM - MIG270TE
Page 30
30
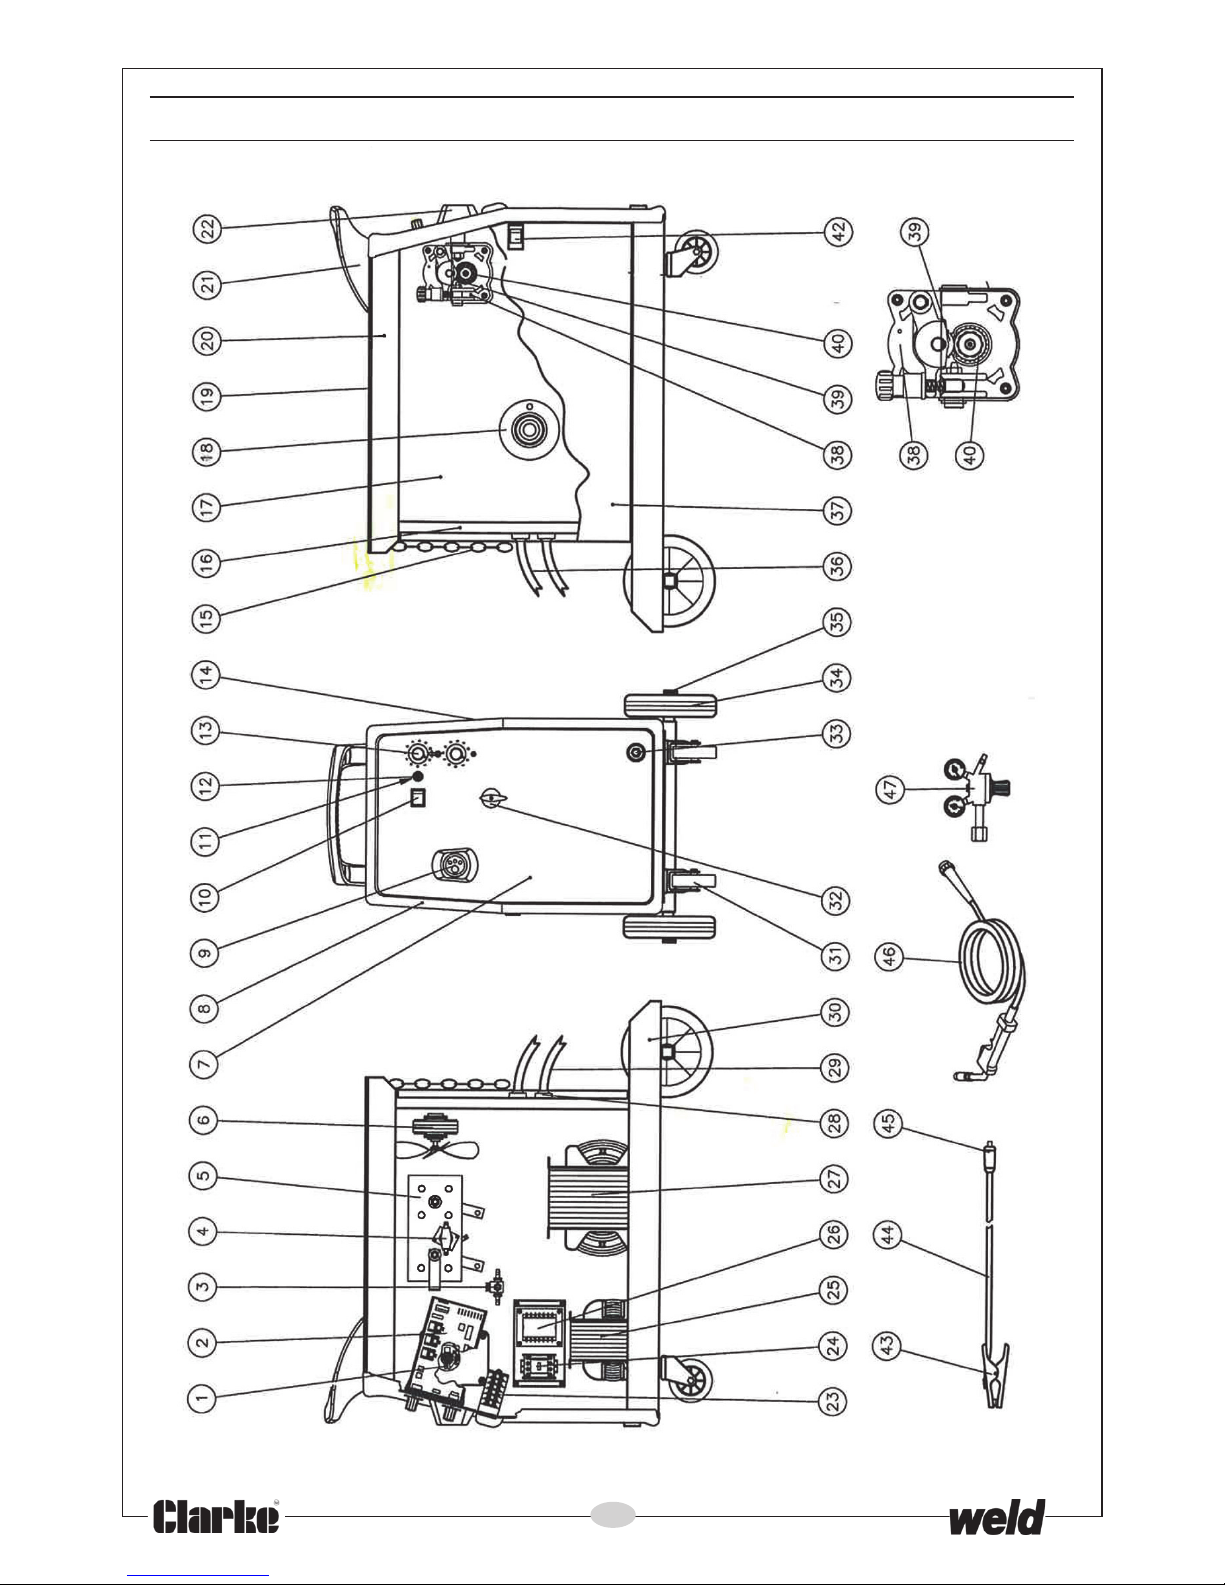
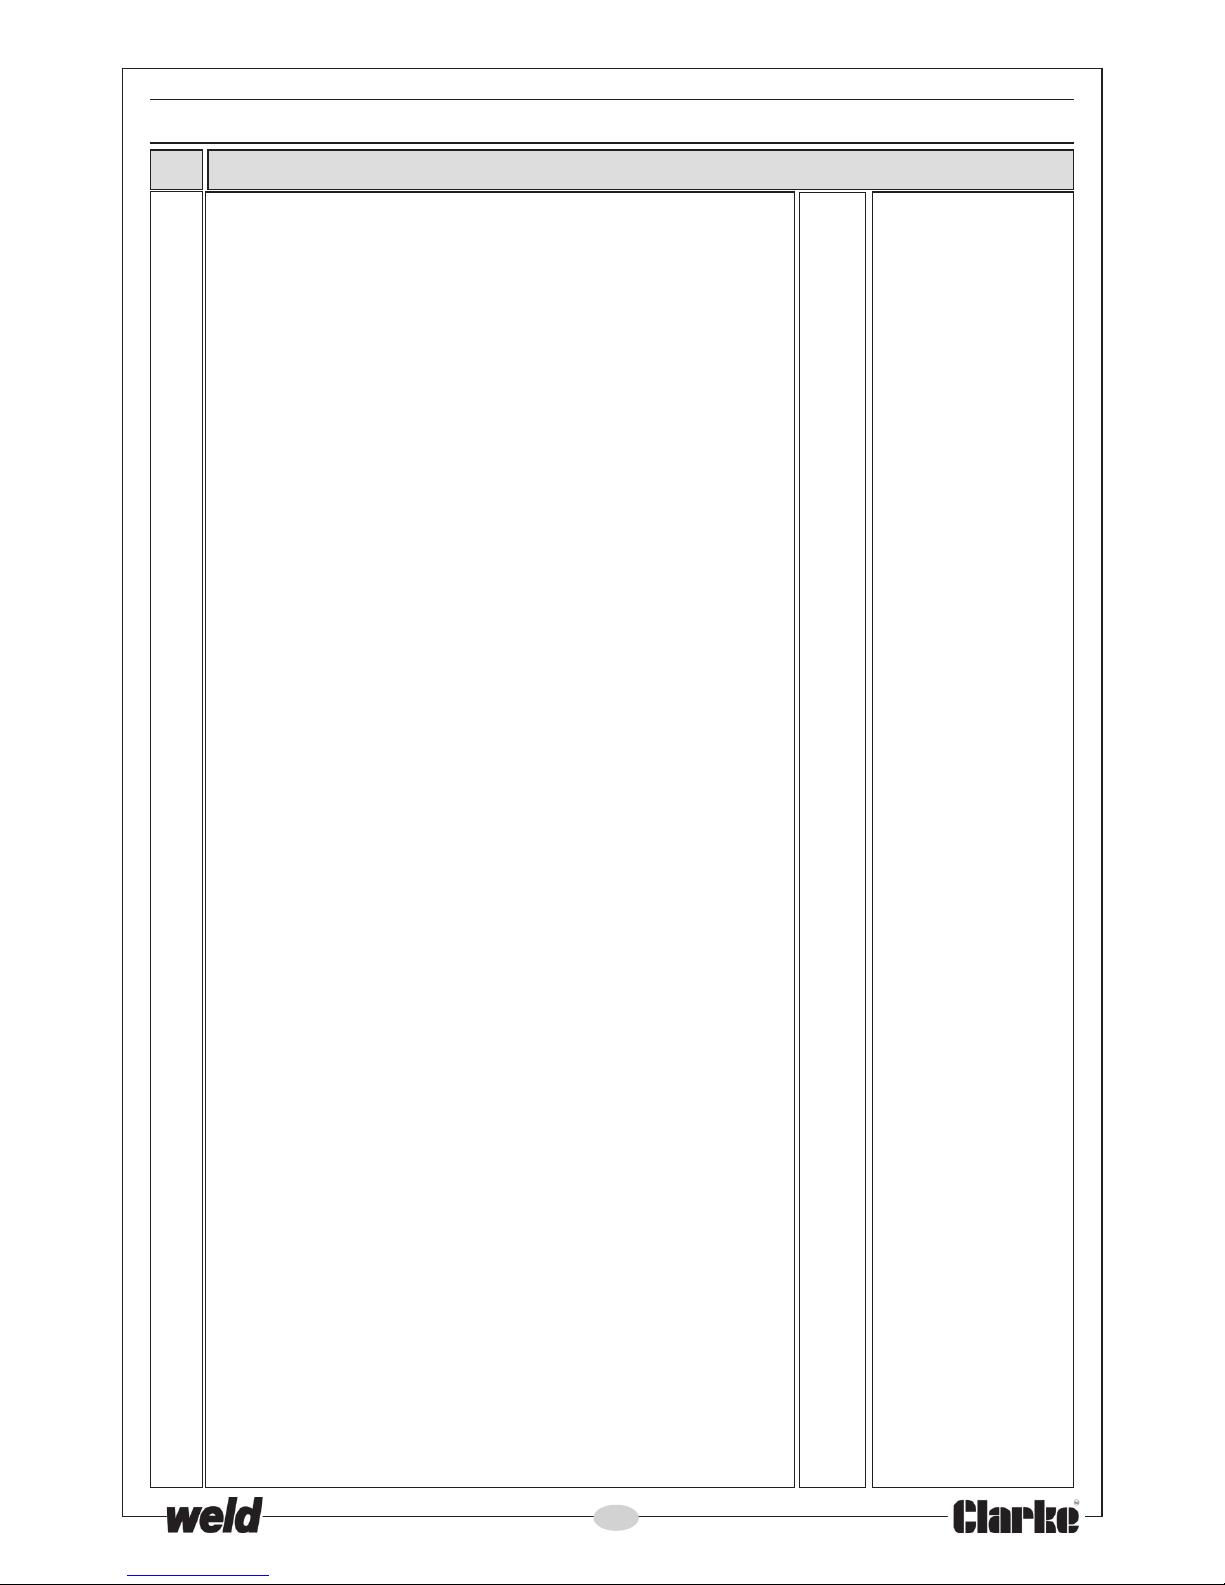
PARTS DIAGRAM - MIG220TE
Page 31
31
PARTS LIST - MIG220TE
No. Description Part No.
01 Motor + Pinion 1 EM04600147
02 Motor Control PCB 1 EM22710190
03 Gas Solenoid Valve 1 EM22900035
04 Thermostat + Support 1 EM04600113
05 Rectifier 1 EM22400085
06 Fan 220V 1 EM22800002
07 Front Panel 1 EM33710295
08 Plastic Front Frame 1 EM21690285
09 Binzel / Euro Torch Adaptor 1 EM23005048
10 On/Off Switch 1 EM22200002
11 Fuse 1A 250V 1 EM22220002
12 Fuse Holder 1 EM22220016
13 Potentiometer Knob 2 EM04600332
14 Right Side Panel 1 EM33705326
15 Zinc Chain 1 EM04600205
16 Rear Panel 1 EM33715096
17 Dividing Panel 1 EM33720211
18 Complete Spool Holder 1 EM04600275
19 Tool Mat 1 EM30905045
20 Upper Panel 1 EM33705628
21 Handle 1 EM21600042
22 Torch Connection Cover 1 EM21690267
23 Switch 20A 1 EM22205033
24 24V Contactor 1 EM22225022
25 Choke 1 EM44135082
26 Auxiliary Transformer 1 EM44140054
27 Transformer 1 EM44120109
28 Cable Clamp 2 EM21605010
29 Input Cable 1 EM20220020
30 Lower Panel 1 EM33700317
31 Castor 2 EM21625003
32 Switch Knob 1 EM21690268
33 Female Dinse Plug 1 EM22100002
34 Rear Wheel 2 EM21625048
35 Wheels Axle 1 EM55200036
36 Black Hose 1 EM30900027
37 Left Access Panel 1 EM33705627
38 Aluminium Wire Feeder + Gear 1 EM44410021
39 Wire Block Roll 1 EM33805007
40 Wire Feed Roll 0,6-0,8mm 1 EM33805003
40 Wire Feed Roll 1,0-1,2mm 1 EM33805005
40 Wire Feed Roll 0,8-1mm 1 EM33805104
42 Slide Clip 1 EM21690226
43 Earth Clamp 300A 1 EM22110033
44 Earth Cable 1 EM43210167
45 Dinse Plug 1 EM22100001
46 Torch 1 EM23000424
47 Reducer c/w Gauge 1 EM22905017
49 Mask 1 EM21905029
50 Clear Glass 1 EM21905020
51 Dark Glass 1 EM21905024
Page 32
32
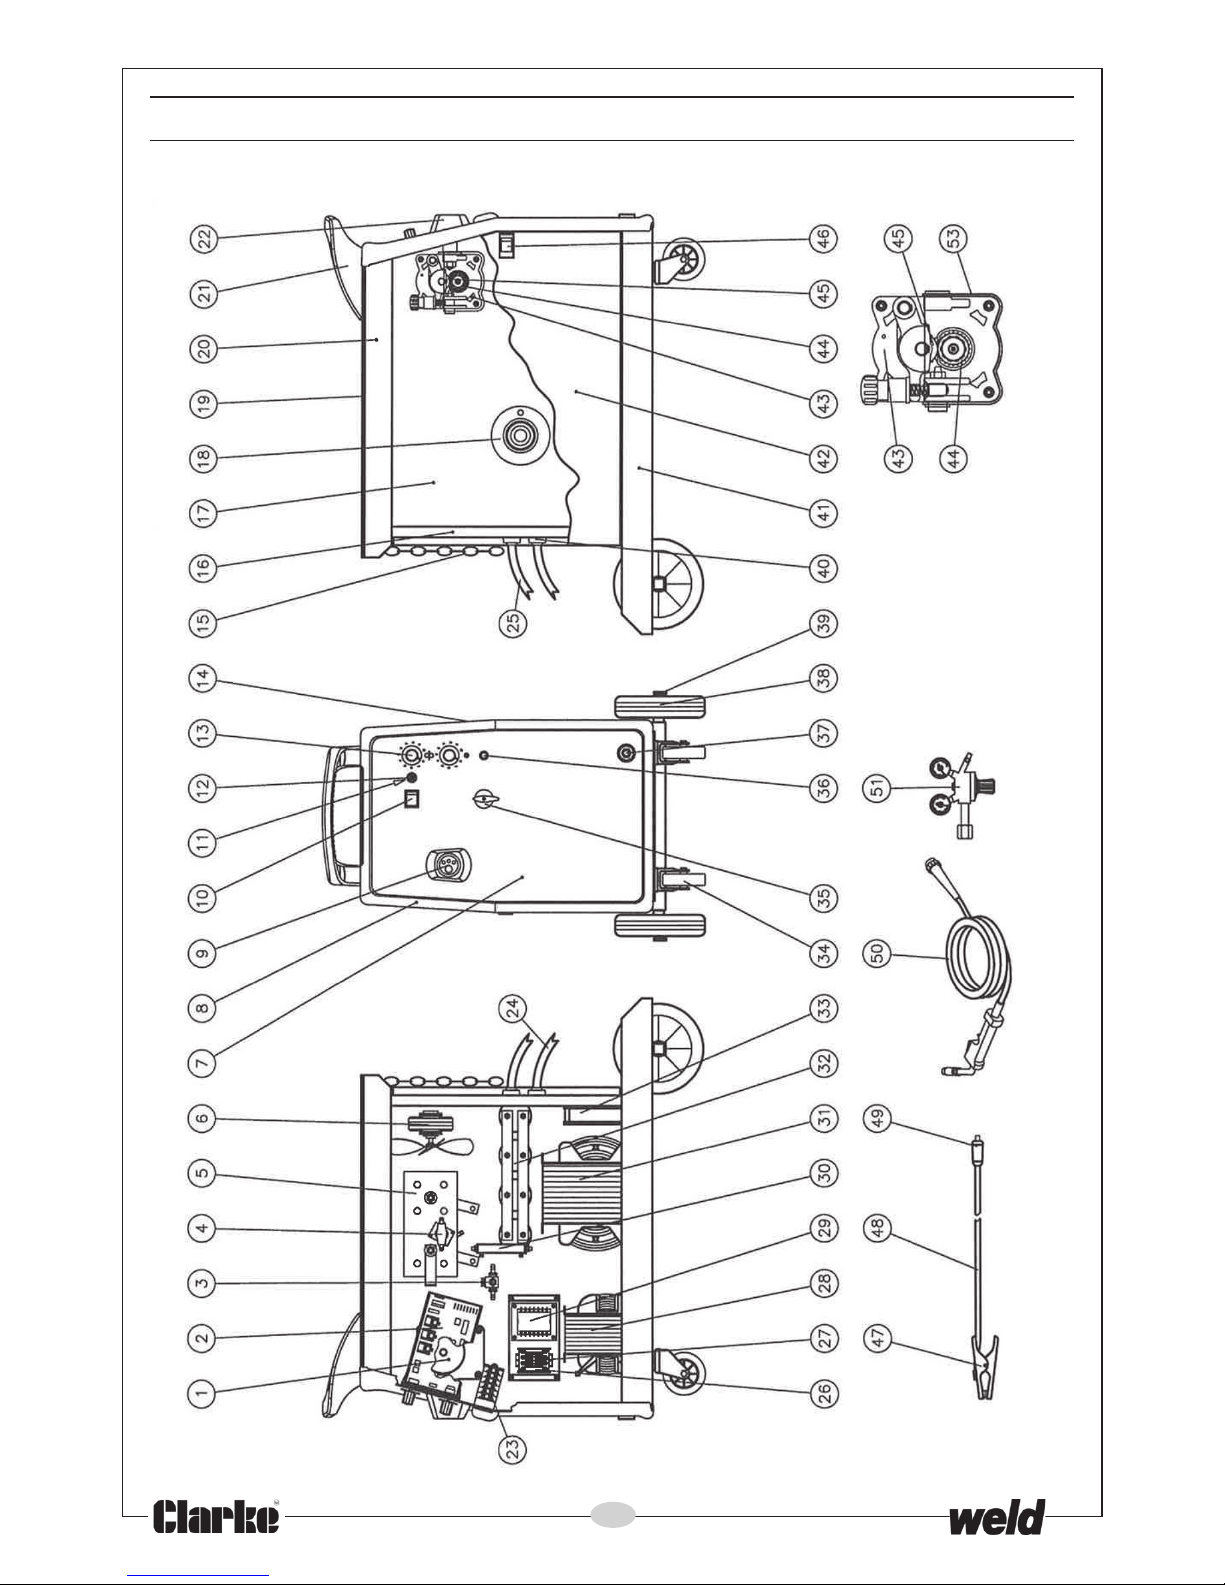
PARTS DIAGRAM - MIG255TEC
Page 33
33
PARTS LIST - MIG255TEC
No. Description Part No. No. Description Part No.
01
02
03
04
05
06
07
08
09
10
11
12
13
14
15
16
17
18
19
20
21
22
23
24
25
26
27
28
29
Wire Feed Motor 42V EM22810006
P.C. Board EM22710051
Gas Solenoid Valve EM22900035
Complete Thermostat EM04600113
Rectifier EM22400086
Fan EM22800002
Front Panel EM33710295
Plastic Front EM21690285
Torch Adaptor EM23005048
On/Off Switch EM22200002
Fuse EM22220002
Fuse Holder EM22220016
Potentiometer Knob EM04600332
Right Side Panel EM33705626
Chain EM04600205
Rear Panel EM33715096
Dividing Panel EM33720211
Complete Spool Holder EM04600275
Mat For Tools EM30905045
Cover Panel EM33705628
Handle EM21600042
Torch Connect Cover EM21690267
Switch EM22205155
Input Cable EM20220136
Black Gas Hose EM30900027
Contactor EM22225022
Auxiliary Contacts EM22225018
Choke EM44135128
Auxiliary Transformer EM44140054
Resistor EM22305004
Transformer EM44120147
Capacitor EM22315003
Complete Fan EM22800021
Castor EM21625003
Switch Knob EM04600268
Orange Pilot-lamp EM22610011
Female Plug EM22100002
Rear Wheel EM21625048
Wheels Axle EM55200036
Cable Clamp EM21605010
Lower Panel EM33700317
Left Access Panel EM33705627
Aluminium wire Feeder EM44410017
Feed Roll 0.6-0.8mm EM33805003
Feed Roll 1.0-1.2mm EM33805005
Feed Roll 0.8-1.0mm nylon EM
33805104
Feed Roll 1.2-1.6mm nylon
EM33805105
Block Roll EM33805007
Slide Clip EM21690226
Earth Clamp EM22110033
Earth Cable EM43210167
Dinse Plug EM22100001
Torch EM23000424
Reducer EM22905017
Face Mask EM21905019
Transparent Glass EM21905020
Dark Glass EM21905024
30
31
32
33
34
35
36
37
38
39
40
41
42
43
44
44
44
44
45
46
47
48
49
50
51
- -
- -
- -
Page 34
34
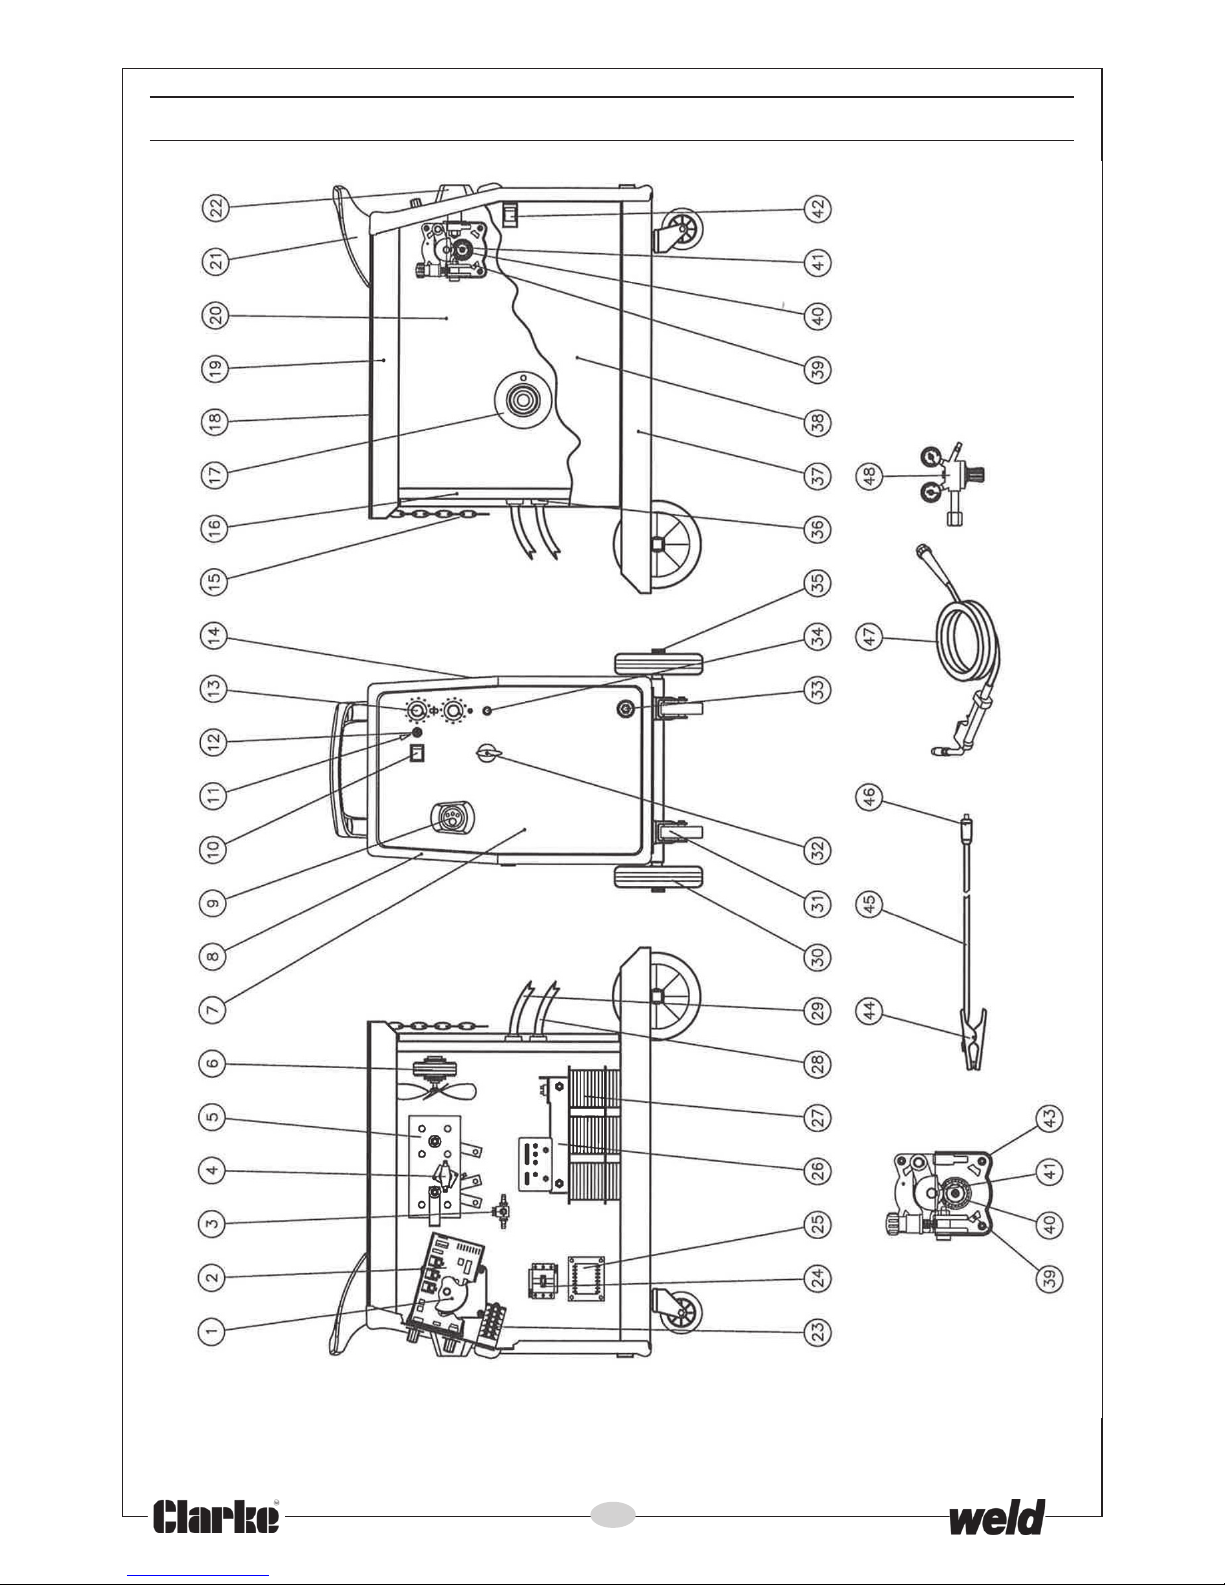
PARTS DIAGRAM - MIG270TE
Page 35
35
28
29
30
31
32
33
34
35
36
37
38
39
40
40
40
41
42
---
44
45
46
47
48
PARTS LIST - MIG270TE
No. Description Part No. No. Description Part No.
01
02
03
04
05
06
07
08
09
10
11
12
13
14
15
16
17
18
19
20
21
22
23
24
25
26
27
Wire Feed Motor 42V EM22810006
P.C. Board EM22710051
Gas Solenoid Valve EM22900035
Thermostat + Support EM04600113
Rectifier EM22400029
Fan EM22800005
Front Panel EM33710295
Front Frame EM21690285
Euro Torch Adaptor EM23005048
Green Pilot-light Switch EM22200005
Fuse 1A 250V EM22220002
Fuse Holder 3A 250V EM22220016
Potentiometer Knob EM04600332
Right Side Panel EM33705626
Zinc Chain 0,76 Mt EM04600205
Rear Panel EM33715096
Compl. Spool Holder EM04600275
Mat For Tools EM30905045
Upper Panel PVC EM33705628
Dividing Panel PVC EM33720211
Handle EM21600042
Torch Connection Cover
EM21690267
Switch 16 A EM22205030
Contactor EM22225022
Auxiliary Transformer EM44140036
Transformer 230/400V EM44125038
Al Side Winding 230V EM44025084
Input Cable EM20220030
Black Hose EM30900027
Rear Wheel EM21625048
Castor EM21625003
Switch Knob EM04600268
Female Dinse Plug EM22100002
Orange Pilot-lamp 24V EM22610011
Wheels Axle EM55200036
Cable Clamp EM21605010
Lower Panel EM33700317
Left Access Panel EM33705627
Al.. Wire Feeder +Gears EM44410017
Wire Feed Roll 0,6-0,8mm
EM33805003
Wire Feed Roll 1,0-1,2mm
EM33805005
Wire Feed Roll 0,8-1mm Nylon
EM33805104
Wire Block Roll EM33805007
Slide Clip EM21690226
- - - - - - - - - - - - - - - - - - - - - - - -
Earth Clamp 300A EM22110033
Earth Cable EM43210167
Dinse Plug EM22100001
Torch-bl/blk Handle EM23000424
Reducer 2/Gauges EM22905018
Face Mask EM21905029
Transparent Glass EM21905020
Dark Glass EM21905024
- -
- -
- -
Page 36
 Loading...