

Page 1
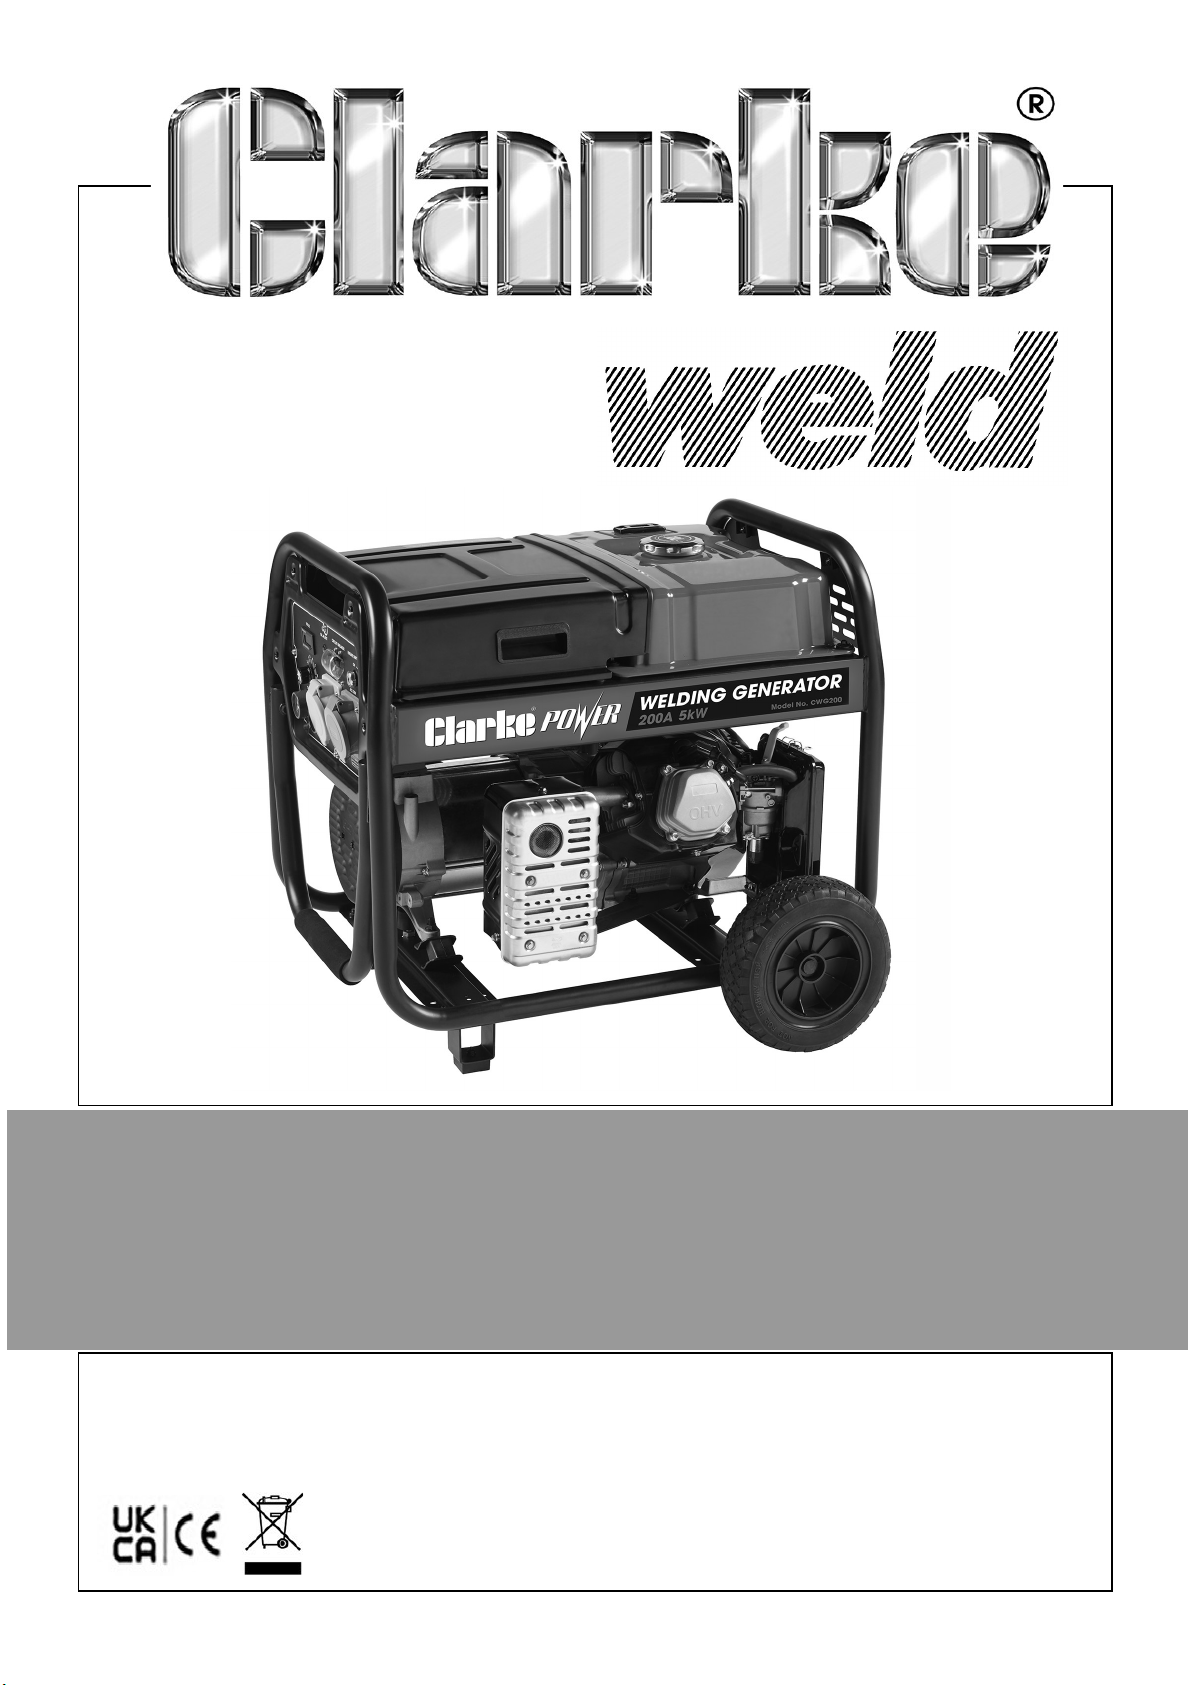
200A 5KW WELDER GENERATOR
MODEL NO: CWG200
PART NO: 8130536
OPERATION & MAINTENANCE
INSTRUCTIONS
ORIGINAL INSTRUCTIONS DL0725
Page 2
INTRODUCTION
Thank you for purchasing this CLARKE Welder Generator designed to provide single
phase electrical power for power or arc welding. No other appliance other than those
indicated should be used with this machine.
Please read through this document and the instruction manuals for the engine and
alternator thoroughly before operating the machine. In doing so you will ensure the
safety of yourself and that of others around you. This will also ensure that the welder
generator will give you long and satisfactory service.
It is important that all accompanying instructions are observed. Clarke International
does not accept responsibility for any injury or damage caused through improper use.
Please keep these instructions in a safe place for future reference.
GUARANTEE
This CLARKE product is guaranteed against faulty manufacture for a period of 12
months from the date of purchase. Please keep your receipt as proof of purchase.
This guarantee is invalid if the product is found to have been abused or tampered
with in any way, or not used for the purpose for which it was intended.
Faulty goods should be returned to their place of purchase, no product can be
returned to us without prior permission. This guarantee does not effect your statutory
rights.
ENVIRONMENTAL RECYCLING POLICY
By purchasing this product, the customer is taking on the obligation to
deal with its safe disposal in accordance with the Waste Electrical and
Electronic Equipment (WEEE).
In effect, this means that this product must not be disposed of with
general household waste. It must be disposed of according to the laws
governing at a recognised disposal facility.
Please note that the details and specifications contained herein, are correct at the
time of going to print. However, CLARKE International reserve the right to change
specifications at any time without prior notice. ALWAYS CONSULT THE
MACHINE’S DATA PLATE.
2
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 3
SAFETY SYMBOLS
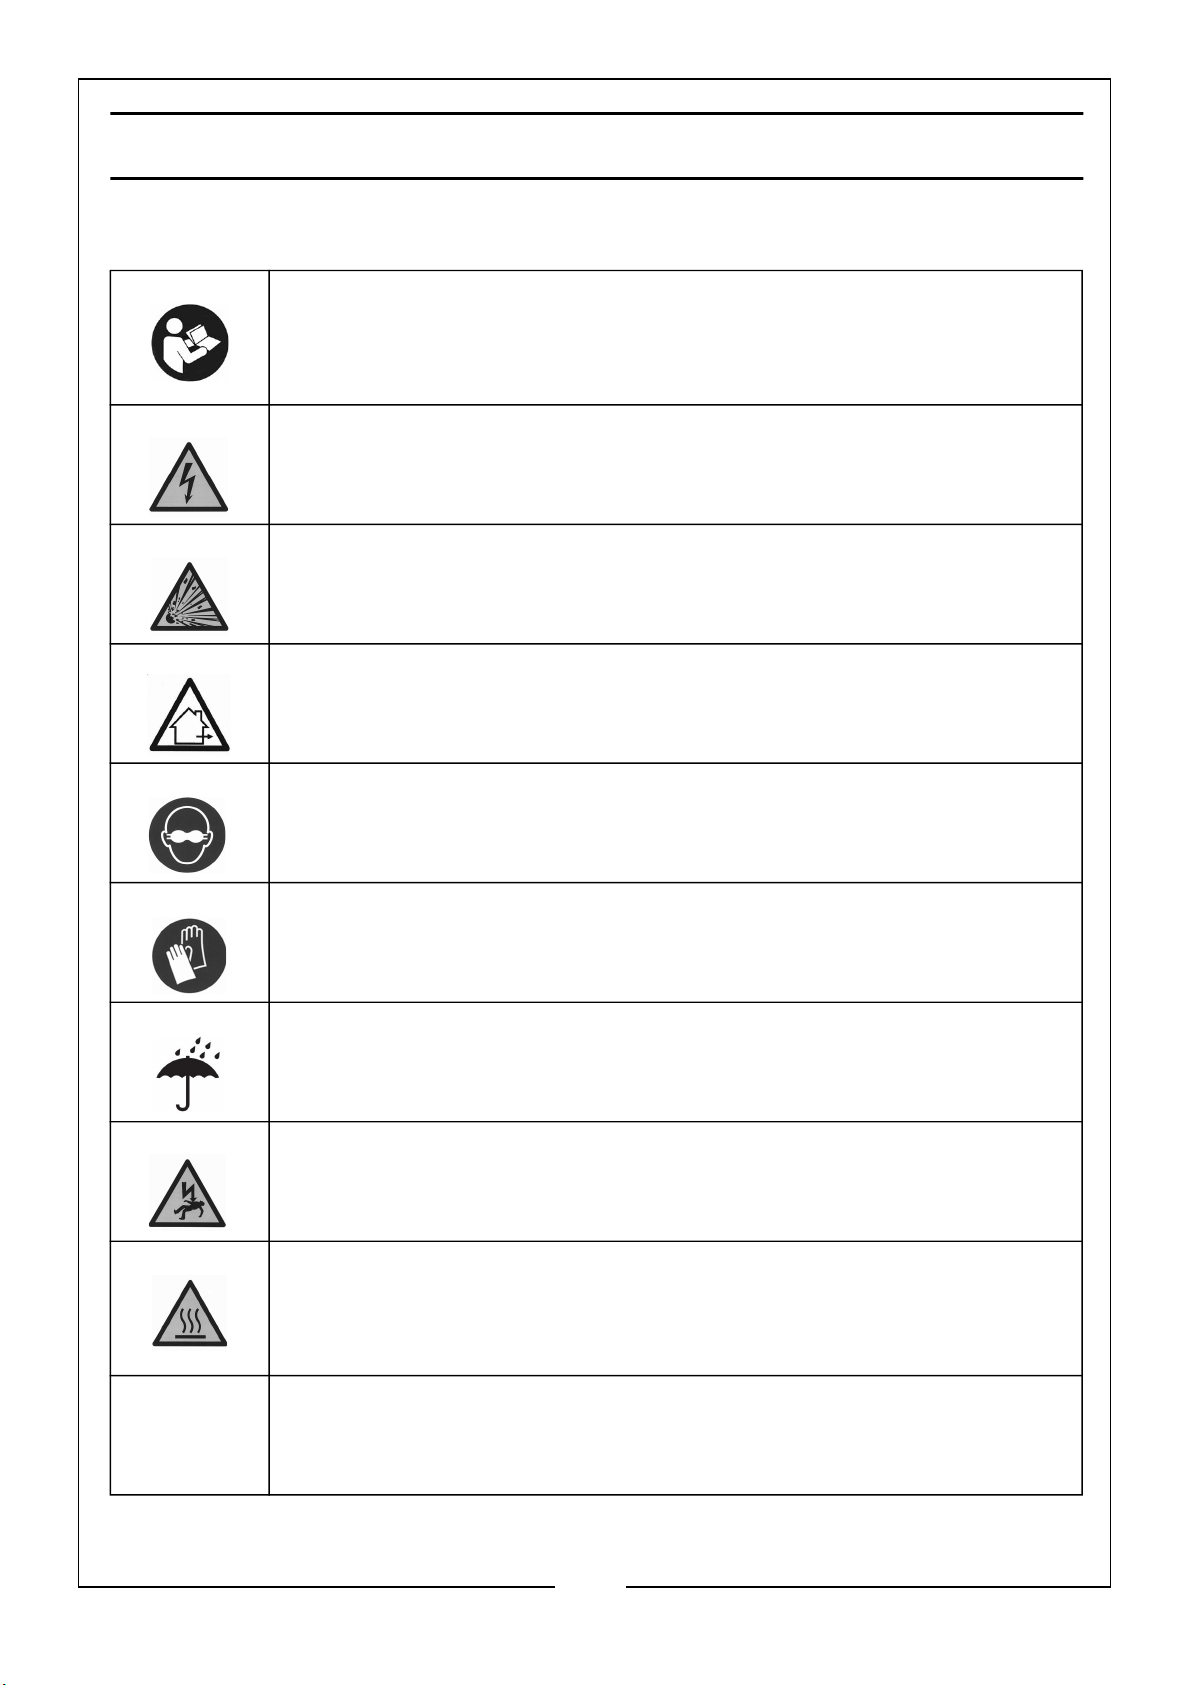
ALWAYS: Read this manual and make sure that all warnings and
instructions are clear before you use this pressure washer.
WARNING: Generator must be provided with an appropriate earth.
DANGER: Risk of fire or explosion. Stop the engine before you refuel
the generator. Keep flammable materials away from the work area.
DANGER: Risk to br ea thin g. E ng in e ex haust fumes can kill.
For outdoor use only. Work in a well ventilated area.
WARNING: Opaque eye protection should be worn at all times
while welding.
WARNING: Wear Protective Gloves.
WARNING: DO NOT use in the rain
WARNING: Risk of electrocution.
WARNING: Risk of hot surfaces. Avoid contact with hot engine
exhaust components. DO NOT allow contact with the engine
muffler during or after use.
WARNING: Loud Noise, risk to hearing.
3
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 4
PREPARATION OF THE WORKING AREA
The working area must be sufficiently spacious, with low humidity and well-ventilated
so as to avoid any fumes which develop from the welding process and from incidental
material adhering to the pieces to be welded (oils, paints, tars...) which may cause
danger to the operator.
Avoid welding by contact with humid parts nearby combustible liquids. Least of all, do
not weld upon tanks which may contain inflammable residuals.
WARNING: ELECTRIC SHOCK CAN BE FATAL. A PERSON QUALIFIED
IN FIRST AID SHOULD ALWAYS BE PRESENT IN THE WORKING
AREA. IF PERSON IS UNCONSCIOUS AND ELECTRIC SHOCK IS
SUSPECTED, DO NOT TOUCH THE PERSON IF HE OR SHE IS IN
CONTACT WITH THE WELDER OR CABLES. TURN OFF THE
GENERATOR AND THEN USE FIRST AID. DRY WOOD, OR OTHER
INSULATING MATERIAL CAN BE USED TO MOVE CABLES, IF
NECESSARY, AWAY FROM THE PERSON.
FIRE PREVENTION
• ALWAYS switch the engine OFF when refuelling.
• ALWAYS refuel away from any source of heat.
• ALWAYS refuel in a well ventilated area.
• NEVER overfill fill the tank, fill to the level specified.
• NEVER smoke whilst refuelling and avoid smoking or using a naked flame near
the generator.
• NEVER start the engine if there is a fuel spill. Any spillage must be wiped clean
and the machine allowed to dry before attempting to start the engine.
PREVENTION OF ELECTRIC SHOCK
• ALWAYS store the generator undercover when not in use and away from damp
or wet conditions.
• NEVER use the generator when it is raining or snowing or in wet or damp
conditions.
• NEVER operate the generator with wet hands.
• NEVER use water or any other liquids to clean the generator.
POSITIONING THE MACHINE FOR USE
• ALWAYS leave at least a 1 metre gap between the generator and any
surrounding building or structure.
• ALWAYS ensure the generator is on a solid, flat surface.
4
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 5
• ALWAYS ensure the surrounding area is free from any material that could burn or
be damaged by heat.
• NEVER move or tilt the generator whilst it is switched on.
• NEVER cover or enclose the generator whilst it is in use.
• Be aware of the weight of the generator, DO NOT attempt to lift or move the
generator without assistance or suitable lifting equipment.
EXHAUST GAS PRECAUTIONS
WARNING!: EXHAUST FUMES CAN BE FATAL
• ALWAYS ensure that there is adequate ventilation when using the generator.
• ALWAYS position the generator so that the exhaust is pointing away from people
or animals.
• If the machine is to be used indoors the exhaust MUST be piped to atmosphere.
ADDITIONAL SAFETY PRECAUTIONS FOR ARC WELDING
• NEVER attempt to remove any of the panels or covers unless the generator is
turn off.
• NEVER use the generator with any of the panels or covers removed.
• NEVER attempt any electrical or mechanical repair unless your are a qualified
technician. If you have a problem with the machine contact your local CLARKE
dealer.
• NEVER use or store in a wet/damp environment. DO NOT EXPOSE TO RAIN.
• NEVER allow children or animals in the vicinity of a welding operation.
• ALWAYS remove all flammable materials from the welding area.
• ALWAYS ensure that there is full free air circulating around the outer casing of
the generator.
• Welding arc can seriously damage your eyes. Both the operator and any
spectators should ALWAYS use a proper welding face shield or helmet, with
suitable filter lenses. Proper gloves and working clothes should be worn at all
times.
• ALWAYS wear a pair of safety spectacles/goggles when chipping away slag after
welding. Remember, ordinary eye glasses are not safety gases.
• ALWAYS ensure there is adequate ventilation or extraction in the work area as
the welding process gives off toxic fumes.
• ALWAYS ensure there is a fire extinguisher on hand.
• ALWAYS ensure that a medical supply is on hand, and that treatment for burns is
provided.
5
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 6
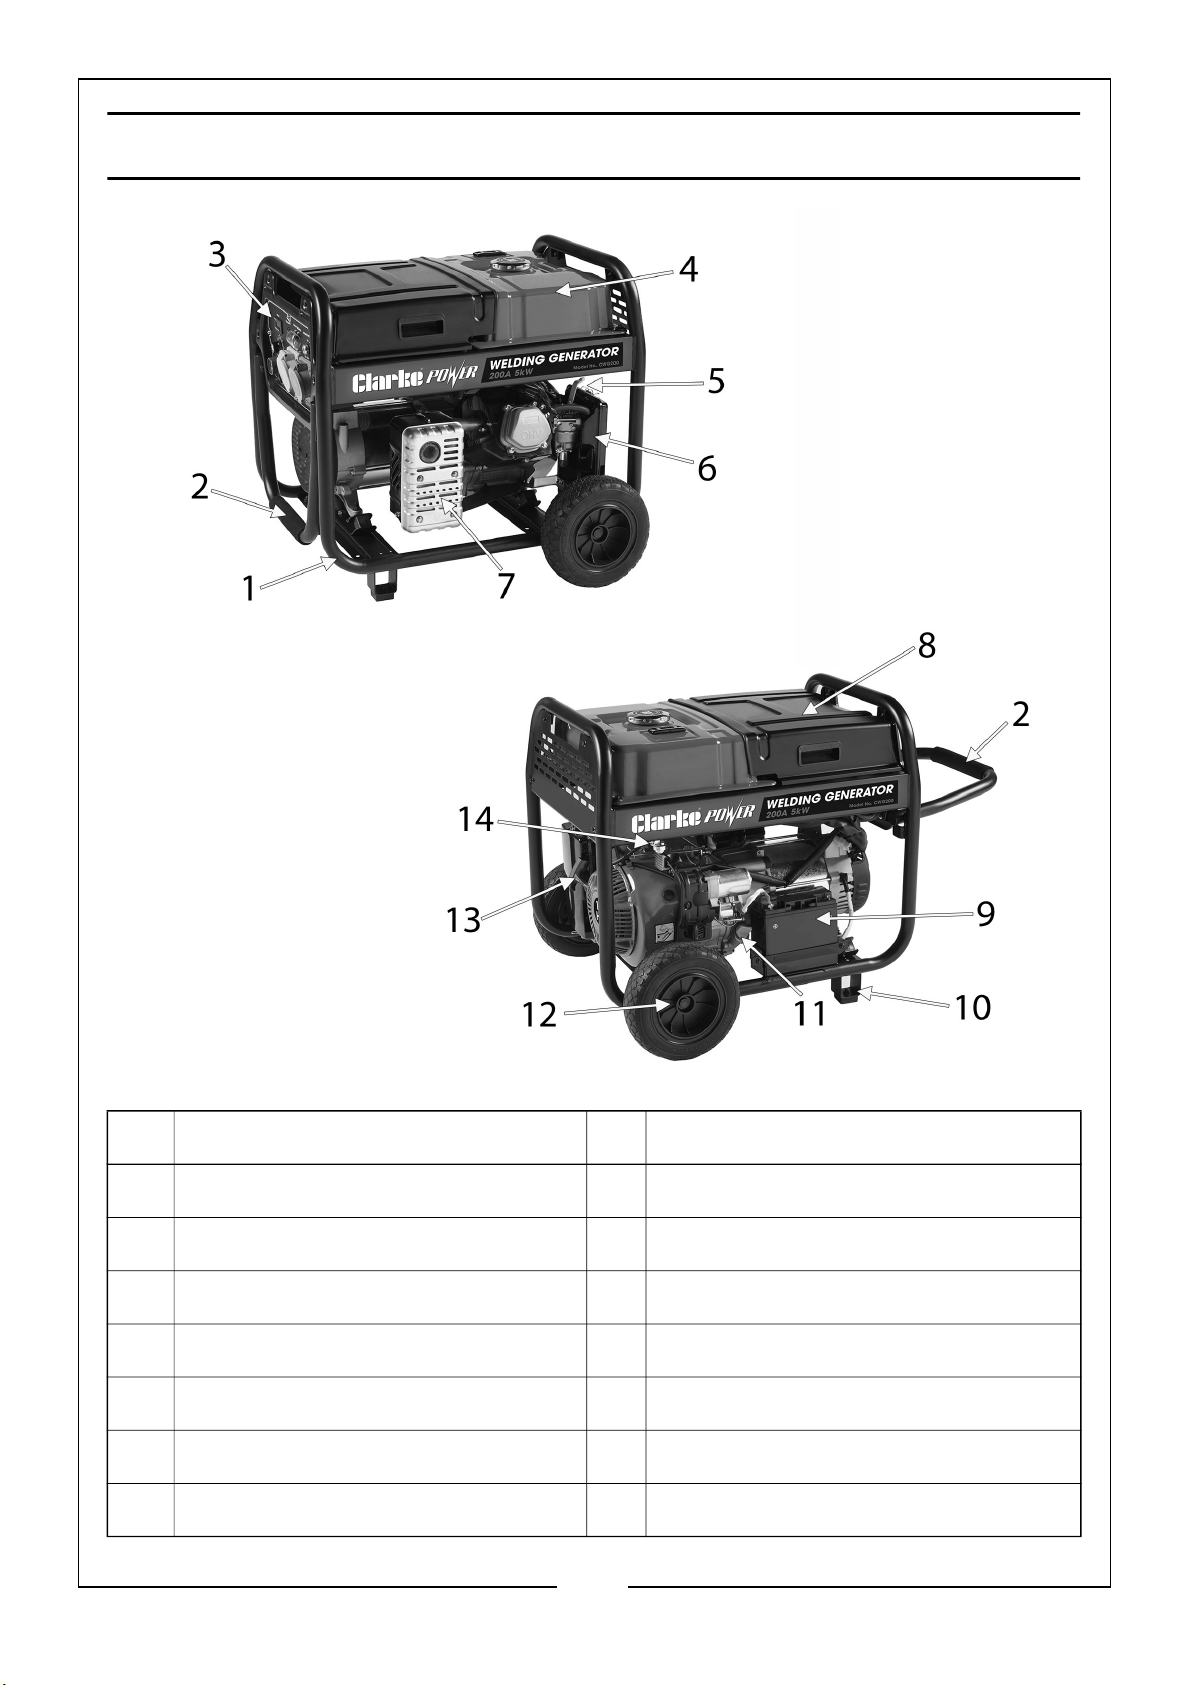
GENERAL OVERVIEW
NO DESCRIPTION NO DESCRIPTION
1 Frame 8 Engine Cover
2 Handle 9 Battery
3 Control Panel 10 Support Foot
4 Fuel Tank 11 Oil Dipstick
5 Choke Lever 12 Wheel
6 Air Filter 13 Support Foot
7 Muffler (Exhaust) 14 Fuel Valve
6
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 7
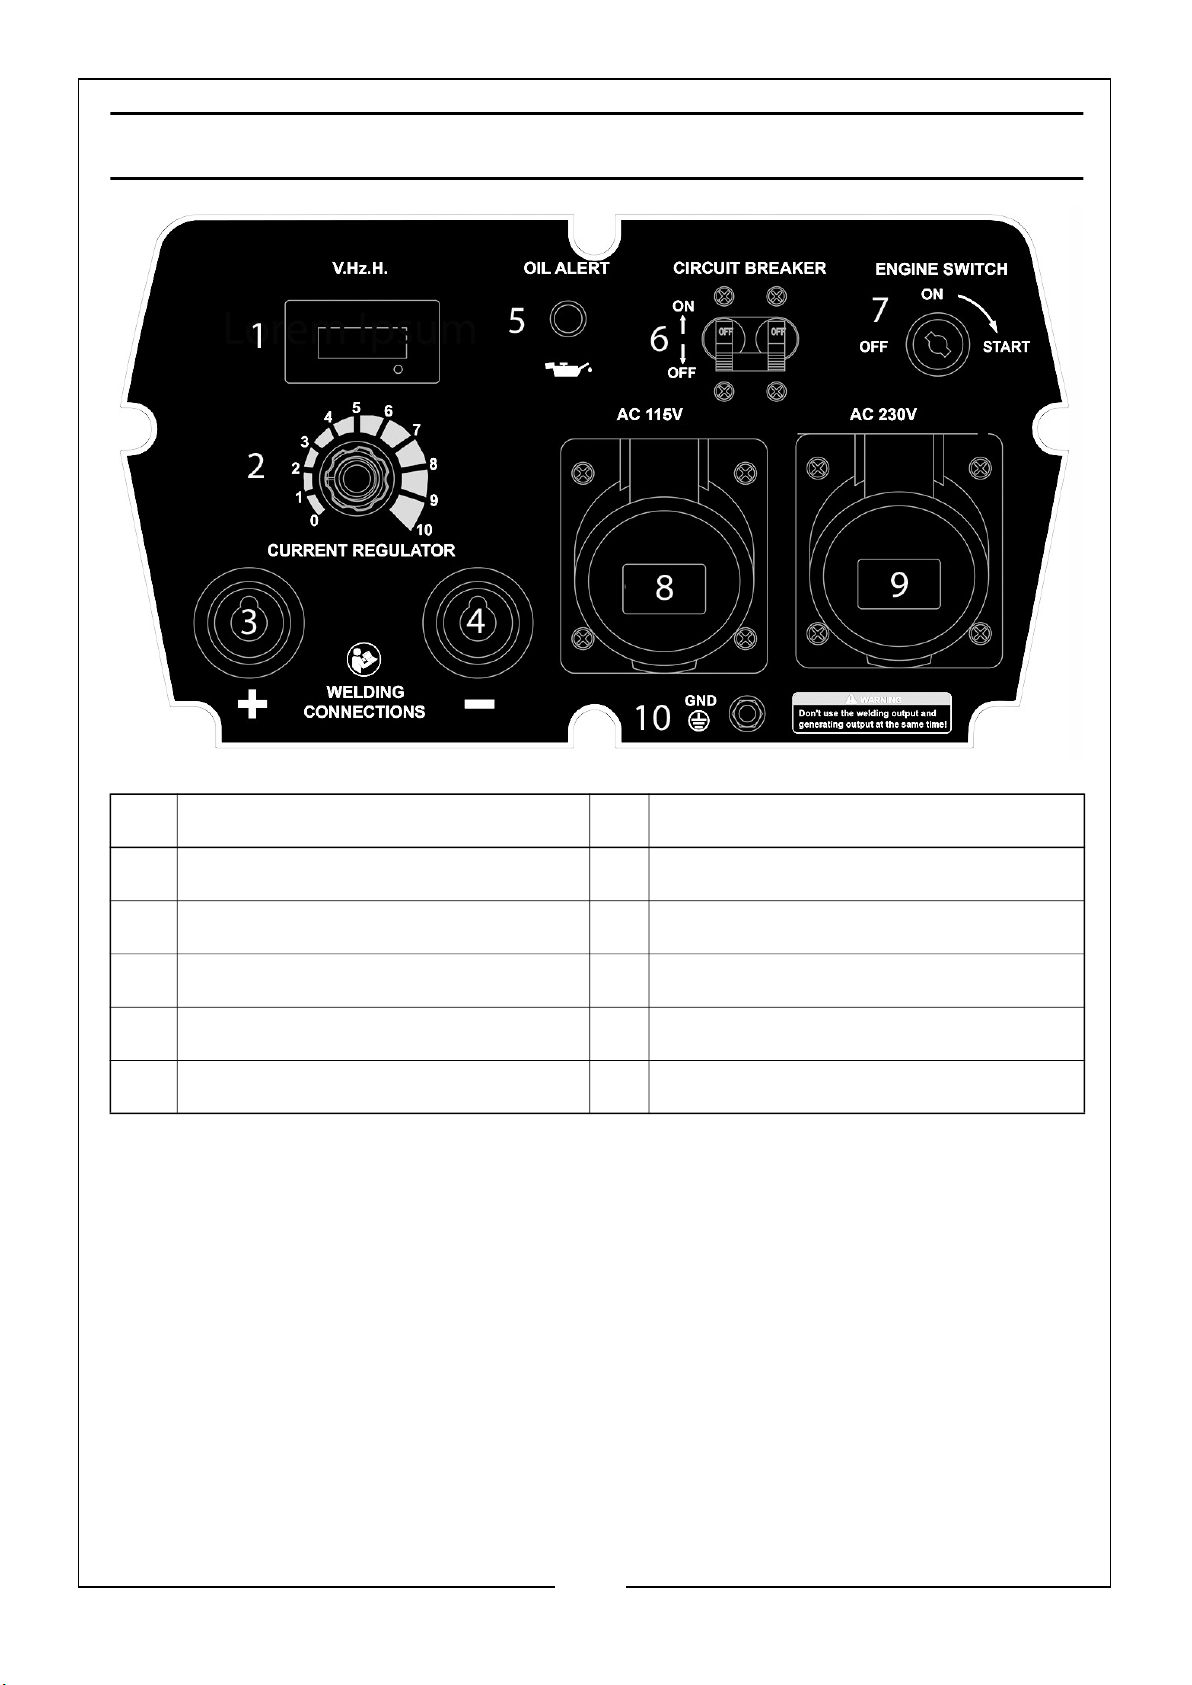
CONTROL PANEL
NO DESCRIPTION NO DESCRIPTION
1 Voltmeter 6 Circuit Breaker
2 Welding Current Regulator 7 Engine Switch/Ignition
3 Welding DIN Socket (Positive) 8 AC 115V Socket
4 Welding DIN Socket (Negative) 9 AC 230V Socket
5 Oil Alert Indicator 10 Earthing Point
7
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 8
ASSEMBLY
WARNING: DUE TO THE WEIGHT OF THIS PRODUCT, IT IS HIGHLY
RECOMMENDED THAT THE UNPACKING AND ASSEMBLY IS CARRIED
OUT BY TWO PERSONS.
UNPACKING
Unpack your welder generator and check to ensure the following items are present.
Contact your CLARKE dealer immediately if any parts are missing or damaged.
1 x Petrol Welder/Generator 1 x Black Welding Earthing Clamp and
Cable
2 x Wheels 1 x Tool Bag
2 x Wheel Axle Rod and Washer 1 x Spark Plug Box Spanner and Arm
2 x ‘R’ Clips 1 x 8mm/10mm Spanner
2 x U Shaped Frame Feet & Fixings 1 x 5mm Hex Key
1 x Red Welding Torch and Cable 1 x Engine Manual
NOTE: Before assembling the wheels and feet, a protective cover should be
placed on the ground and the generator should be placed rear end
down onto it. The control panel should be facing upwards.
FITTING THE WHEELS
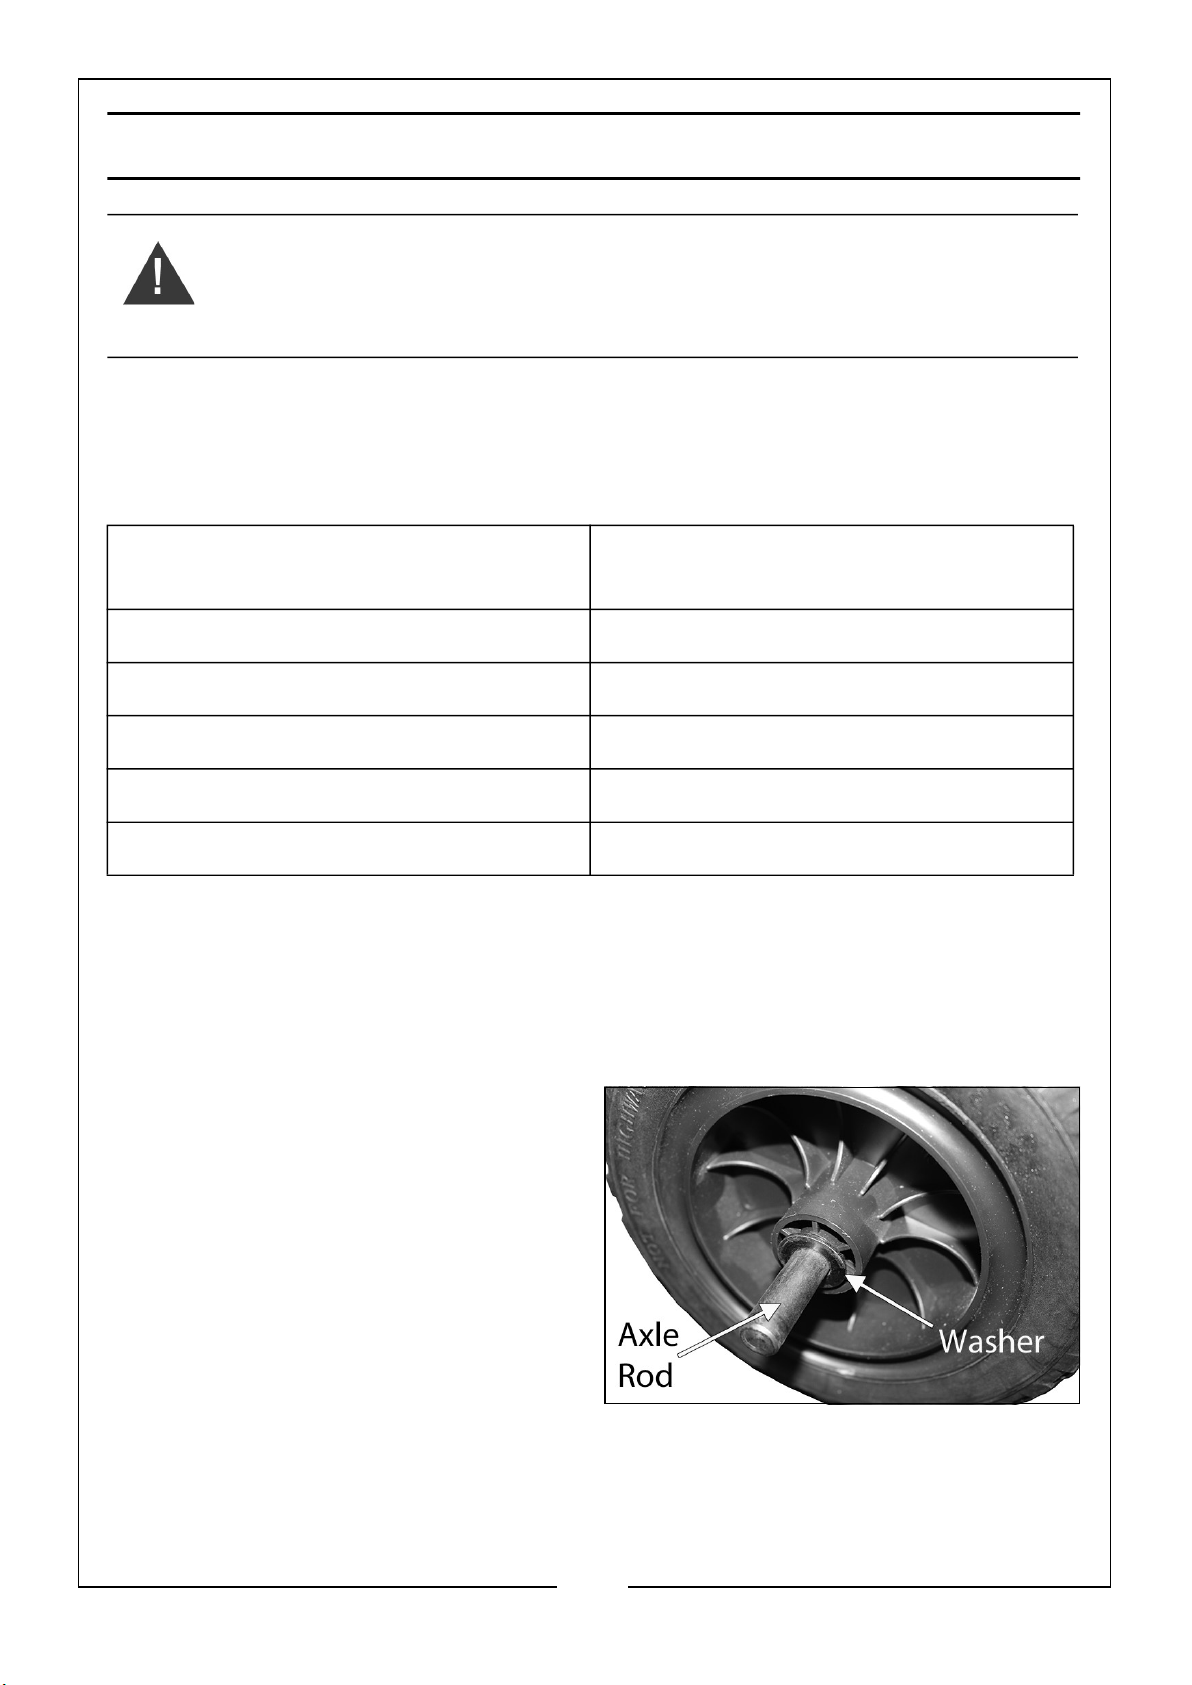
1. On each wheel, slide a washer on to
the axle rod and slide it through the
centre hole in the wheel and slide
another washer onto the axle rod, as
shown.
8
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 9
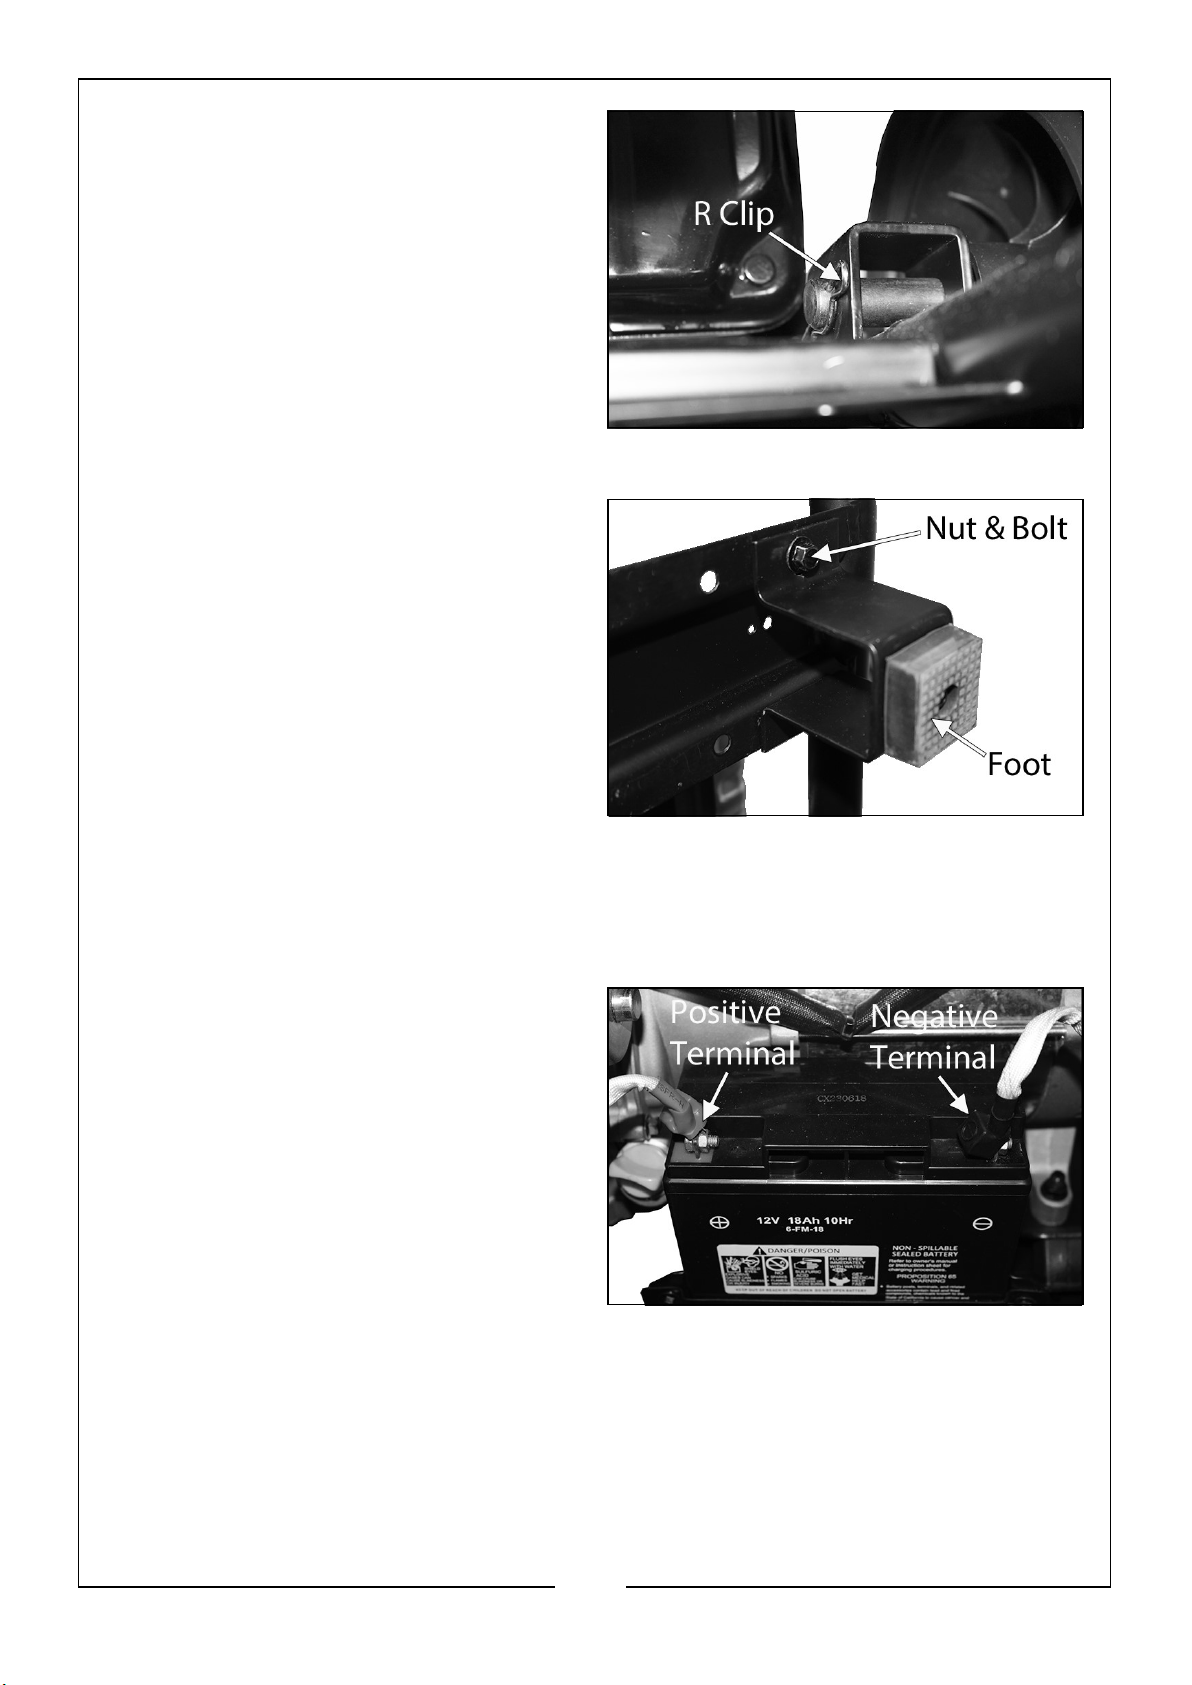
2. Slide each axle rod through the axle
supports on the bottom of the frame
and secure each wheel with an ‘R’
clip that are supplied.
FITTING THE FEET
1. Place a foot on the frame strut (one
each side of the strut), secure in
place with the nut, bolt and washers
supplied, using 8mm and 10mm open
ended spanners.
CONNECTING THE BATTERY
For safety reasons, the generator battery is not connected when shipped. Follow these
steps to connect the battery.
1. Connect the negative wire to the
negative terminal on the battery as
shown.
2. Connect the positive wire to the
positive terminal on the battery as
shown.
3. Ensure both terminals are covered by
the plastic covers.
9
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 10
BEFORE USE
WARNING: STAND THE GENERATOR ON LEVEL GROUND WITH THE
ENGINE SWITCHED OFF.
WARNING: THE OIL LEVEL SHOULD ONLY BE CHECKED WITH A
COLD ENGINE. A HOT ENGINE WILL GIVE A FALSE READING.
IMPORTANT: The engine is supplied without any oil in it and must be
filled to the correct level before starting for the first time, see below.
CHECKING THE ENGINE OIL LEVEL
For safety seasons, the generator is shipped without oil in the engine. Follow these
steps to check and install engine oil.
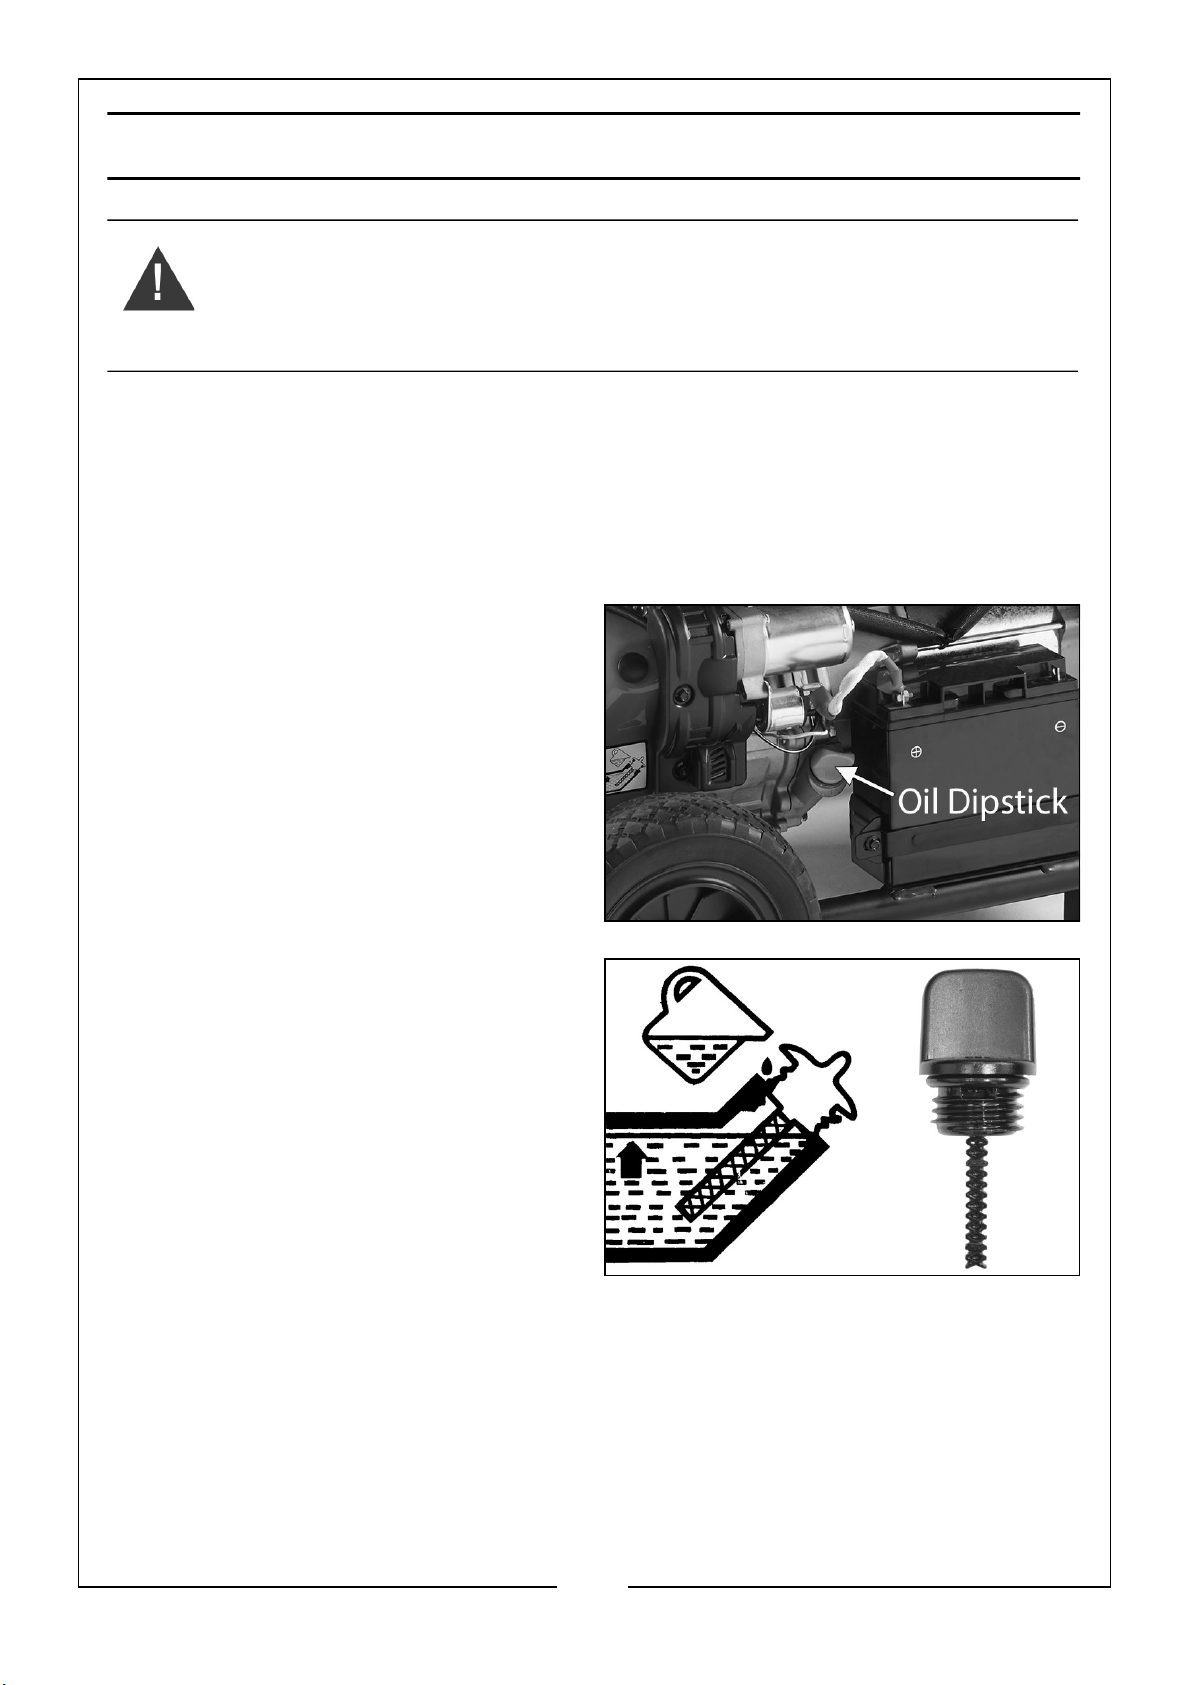
1. Turn the dipstick anti-clockwise and
remove from the oil fill tube.
2. Wipe the dipstick with a clean cloth.
3. Insert the dipstick back into the oil fill
tube and then remove it again. DO
NOT screw in the oil filler cap/
dipstick when doing this.
4. If the oil level is at or below the ‘L’
mark on the dipstick, using a funnel,
add oil to the crankcase.
• Fill until the oil reaches the
threads in the oil fill tube.
• Oil capacity (See page 21).
• We recommend the use of the
following oil: CLARKE SAE30 Motor
Oil; Part No: 3050852
5. Replace the oil filler cap.
10
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 11
CHECKING THE FUEL LEVEL
WARNING: ALWAYS REFUEL IN A WELL VENTILATED AREA AWAY
FROM ANY HEAT SOURCES.
WARNING: ALLOW THE UNIT TO COOL DOWN BEFORE REFUELLING.
WARNING: DO NOT LEAVE FUEL WITHIN THE REACH OF CHILDREN.
For safety seasons, the generator is shipped without petrol in the tank. Follow these
steps to check and install petrol.
RECOMMENDED FUEL
Only use standard unleaded petrol. DO NOT mix oil with the petrol.
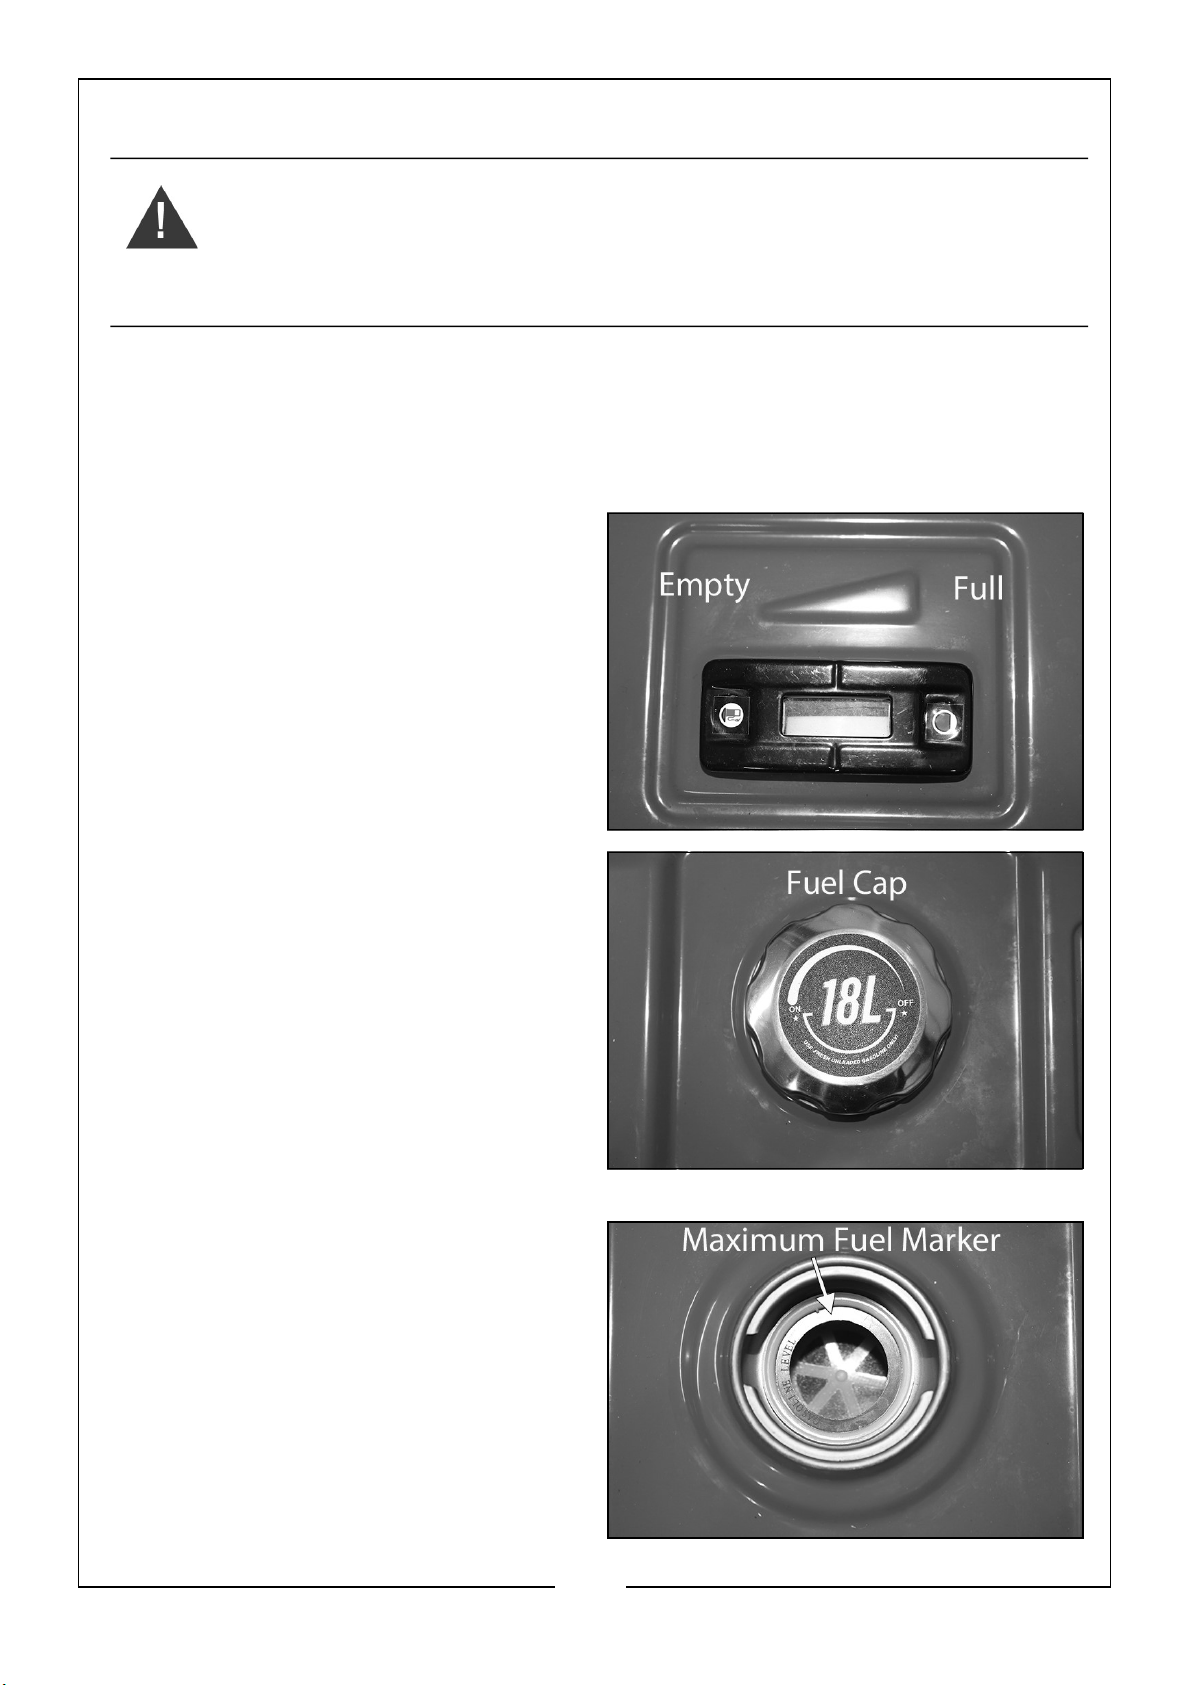
1. Check the fuel level on the fuel
gauge, located on top of the fuel
tank. The fuel gauge will show as red
when you have fuel in the tank
turning white as the fuel level
decreases.
2. To add fuel, open the fuel filler cap.
3. Just inside the fuel tank is a fuel filter
which catches any contaminants as
you refuel.
4. Slowly add fuel to the fuel tank
(maximum 18L) watching the fuel
level gauge as you do so.
NOTE: DO NOT overfill the fuel tank.
NOTE: DO NOT fill above the red fuel
filter marker.
11
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 12
5. Replace the fuel filler cap securely.
EARTH POINT
WARNING: FAILURE TO PROPERLY GROUND THE GENERATOR
BEFORE USE CAN RESULT IN ELECTROCUTION
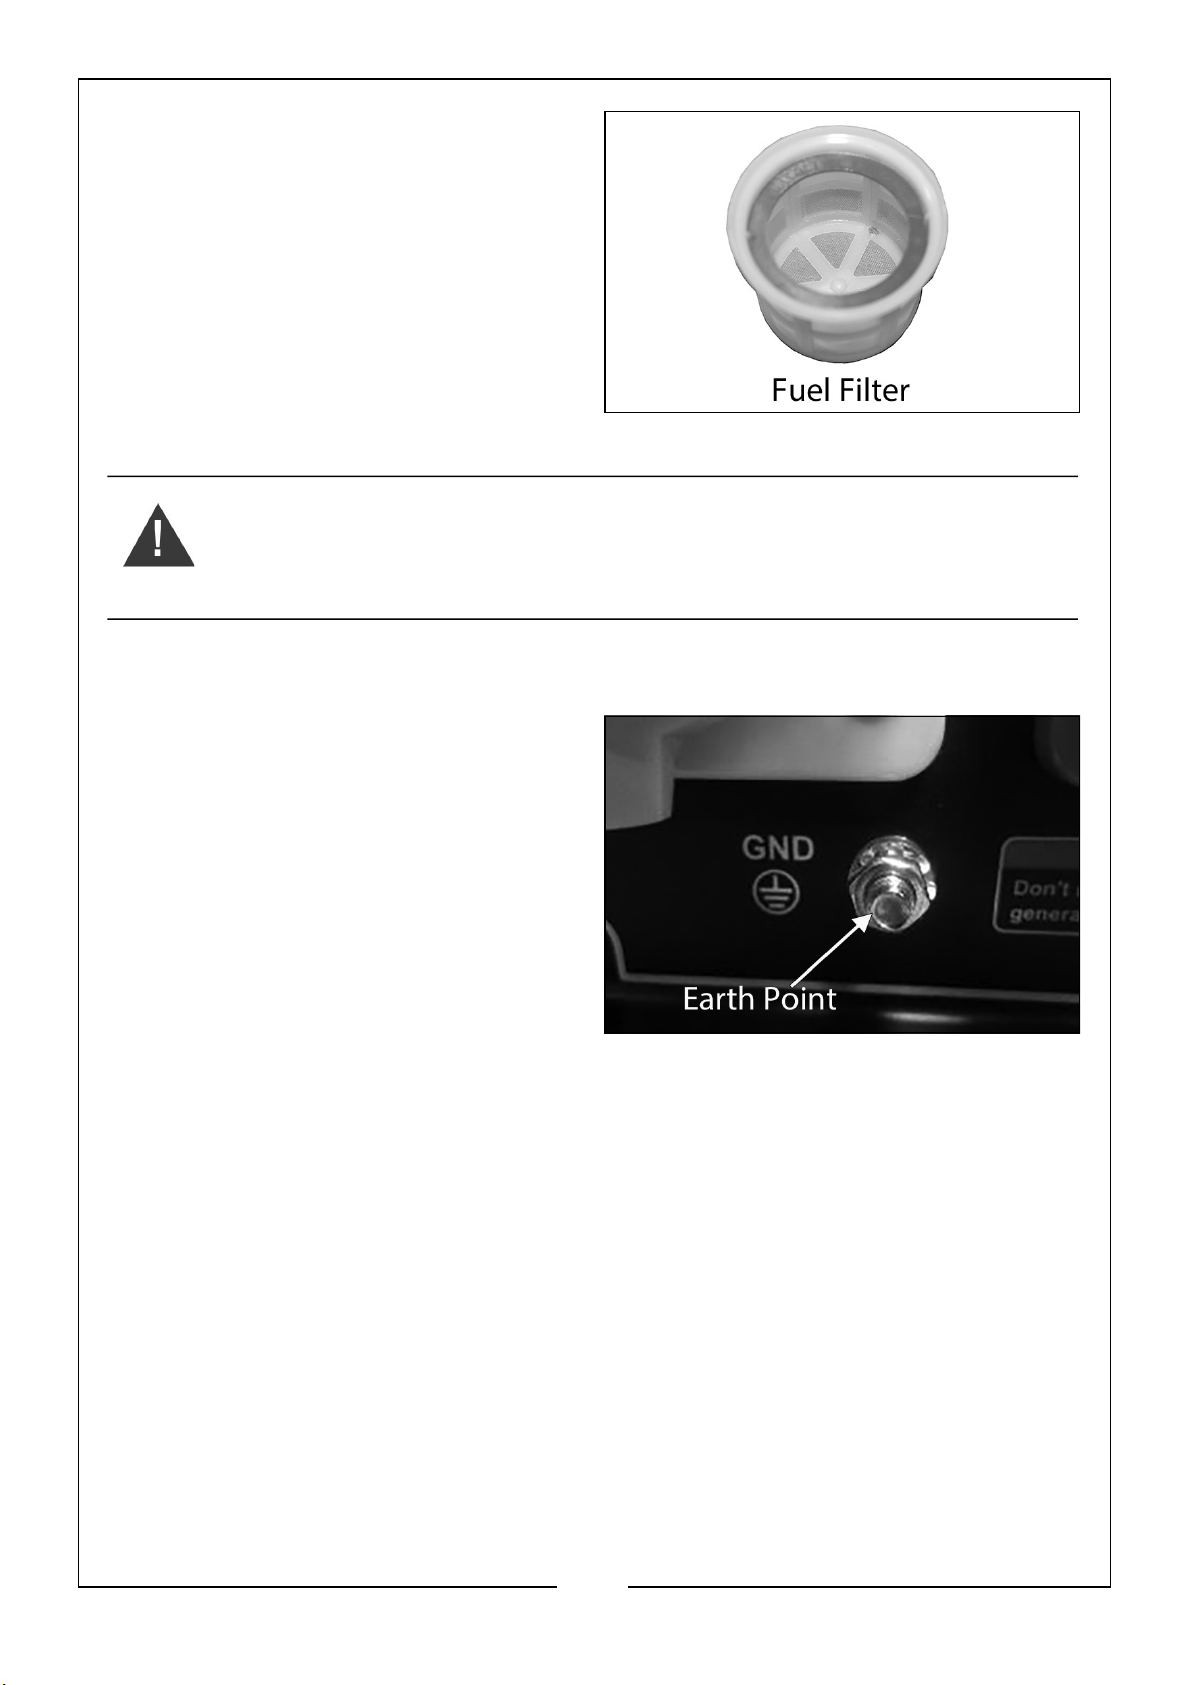
Attach a suitable earth lead to a good earthing point - water pipe, ground spike etc.,
whenever you use this generator.
1. Ground the generator by connecting
a suitable grounding wire to the earth
point, as shown, which is located on
the control panel.
2. Connect the other end of the
grounding wire to a copper or brass
grounding rod or suitable grounding
point that is driven into the earth.
12
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 13
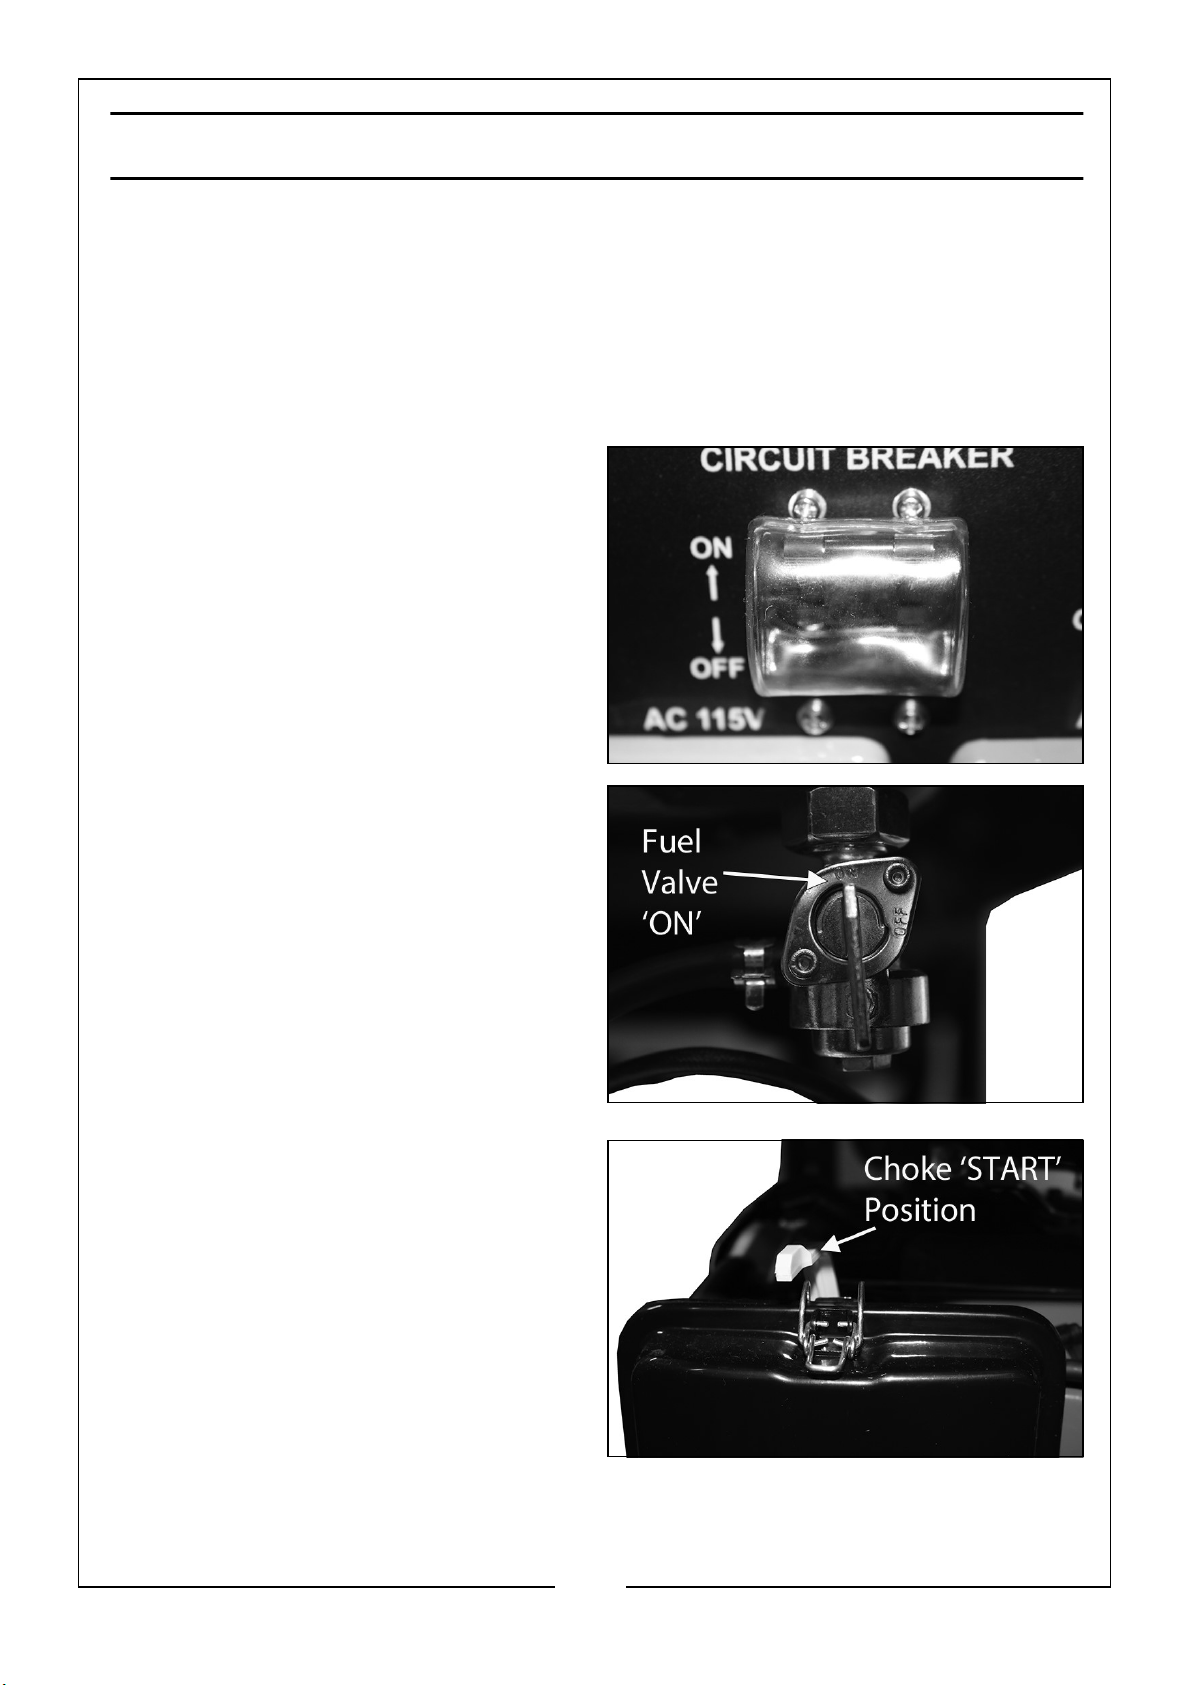
OPERATION - GENERATOR
IMPORTANT: Ensure all precautions are taken, referring to this and the
engine manual, before proceeding.
IMPORTANT: Always check the oil and fuel levels before starting the
engine, see pages 10-11.
STARTING THE ENGINE
1. Remove all connections from the AC
and welding sockets.
2. Switch the AC Circuit Breaker to the
‘ON’ (Up) position.
3. Set the fuel valve to the ‘ON’ position
as shown.
4. Move the choke lever to the ‘START’
position.
NOTE: Move the choke lever to the
‘RUN’ position if starting the
engine in hot condition.
13
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 14
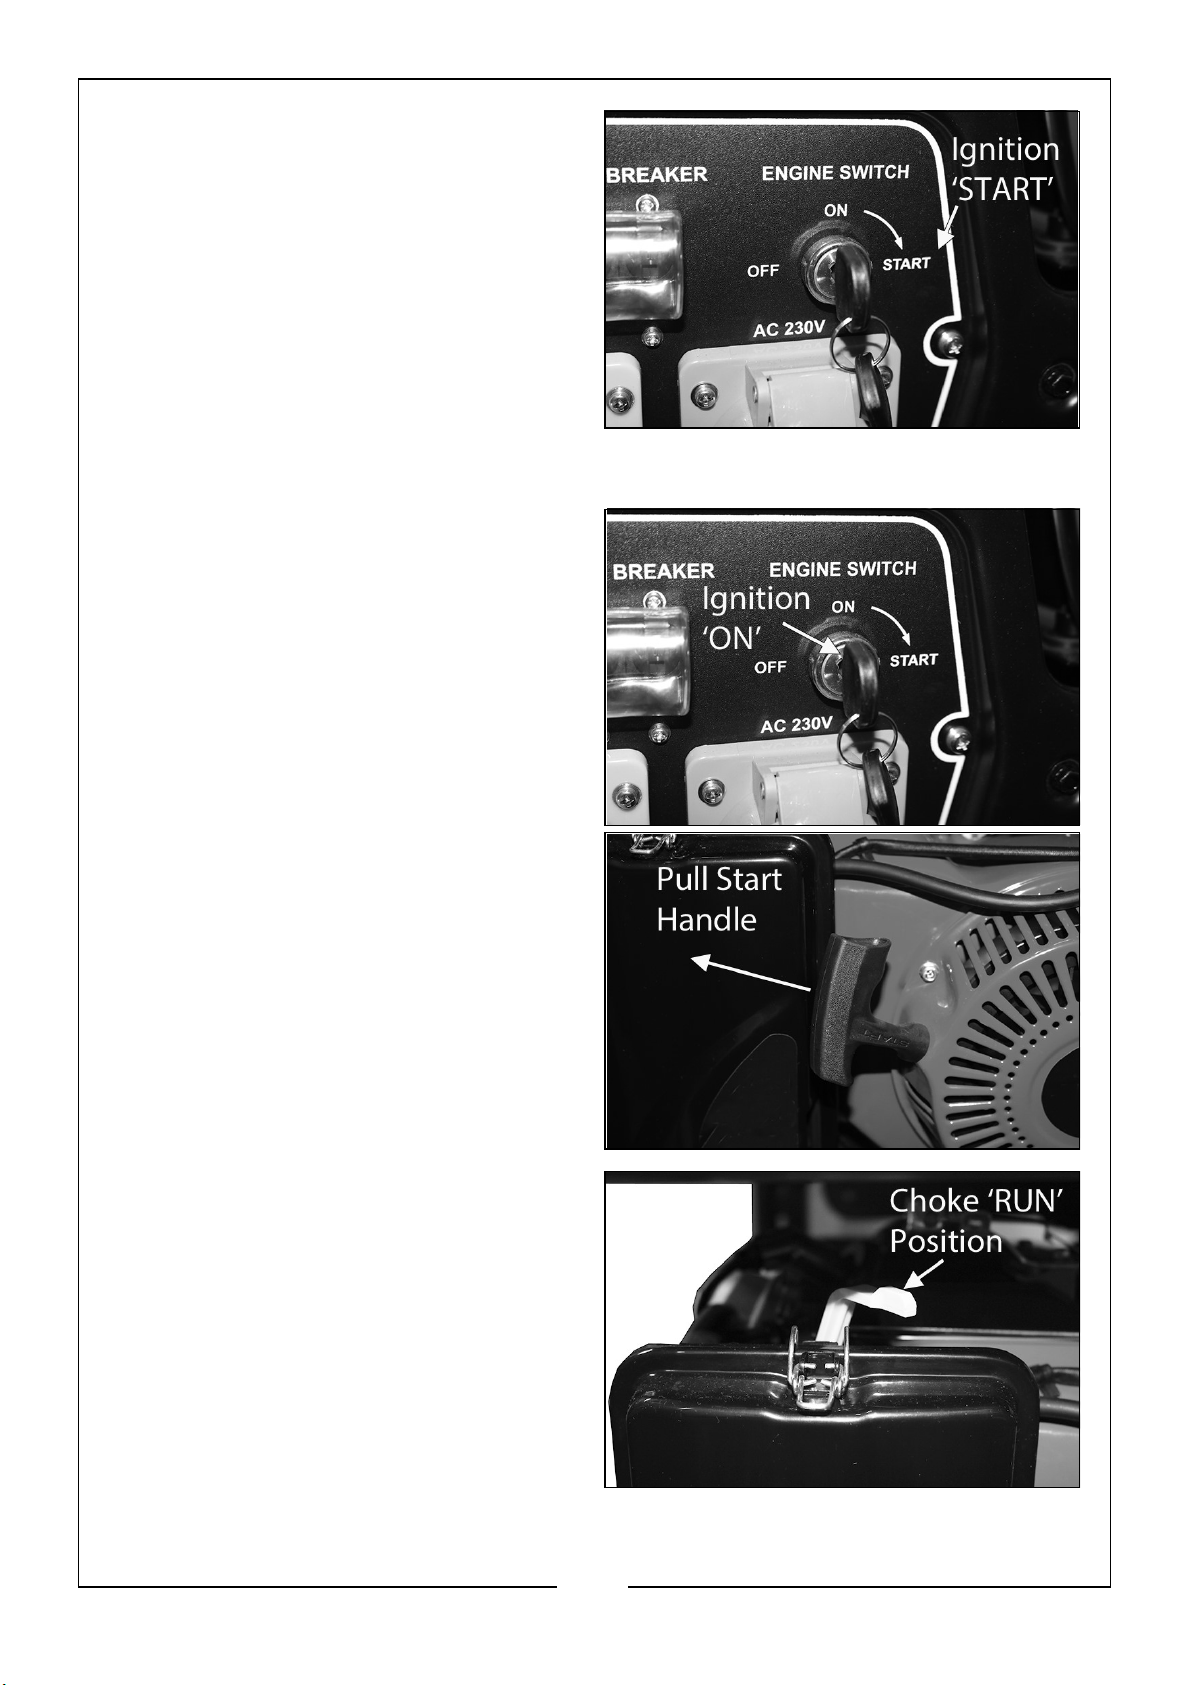
5. Insert the key into the ignition.
6. Turn the key in the ‘START’ position.
NOTE: Once the engine starts, the key
will return to the ‘ON’ position.
7. Once the engine has warmed up, set
the choke lever to the ‘RUN’ position.
ALTERNATIVELY
1. Turn the key to the ‘ON’ position.
2. Pull the start handle gently until you
feel some resistance.
3. Then pull the start handle sharply
upwards.
NOTE: You may have to do this more
than once.
NOTE: NEVER let the handle snap
back, as this may cause damage
to the generator and injury.
4. Once the engine has warmed up, set
the choke lever to the ‘RUN’ position.
14
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 15
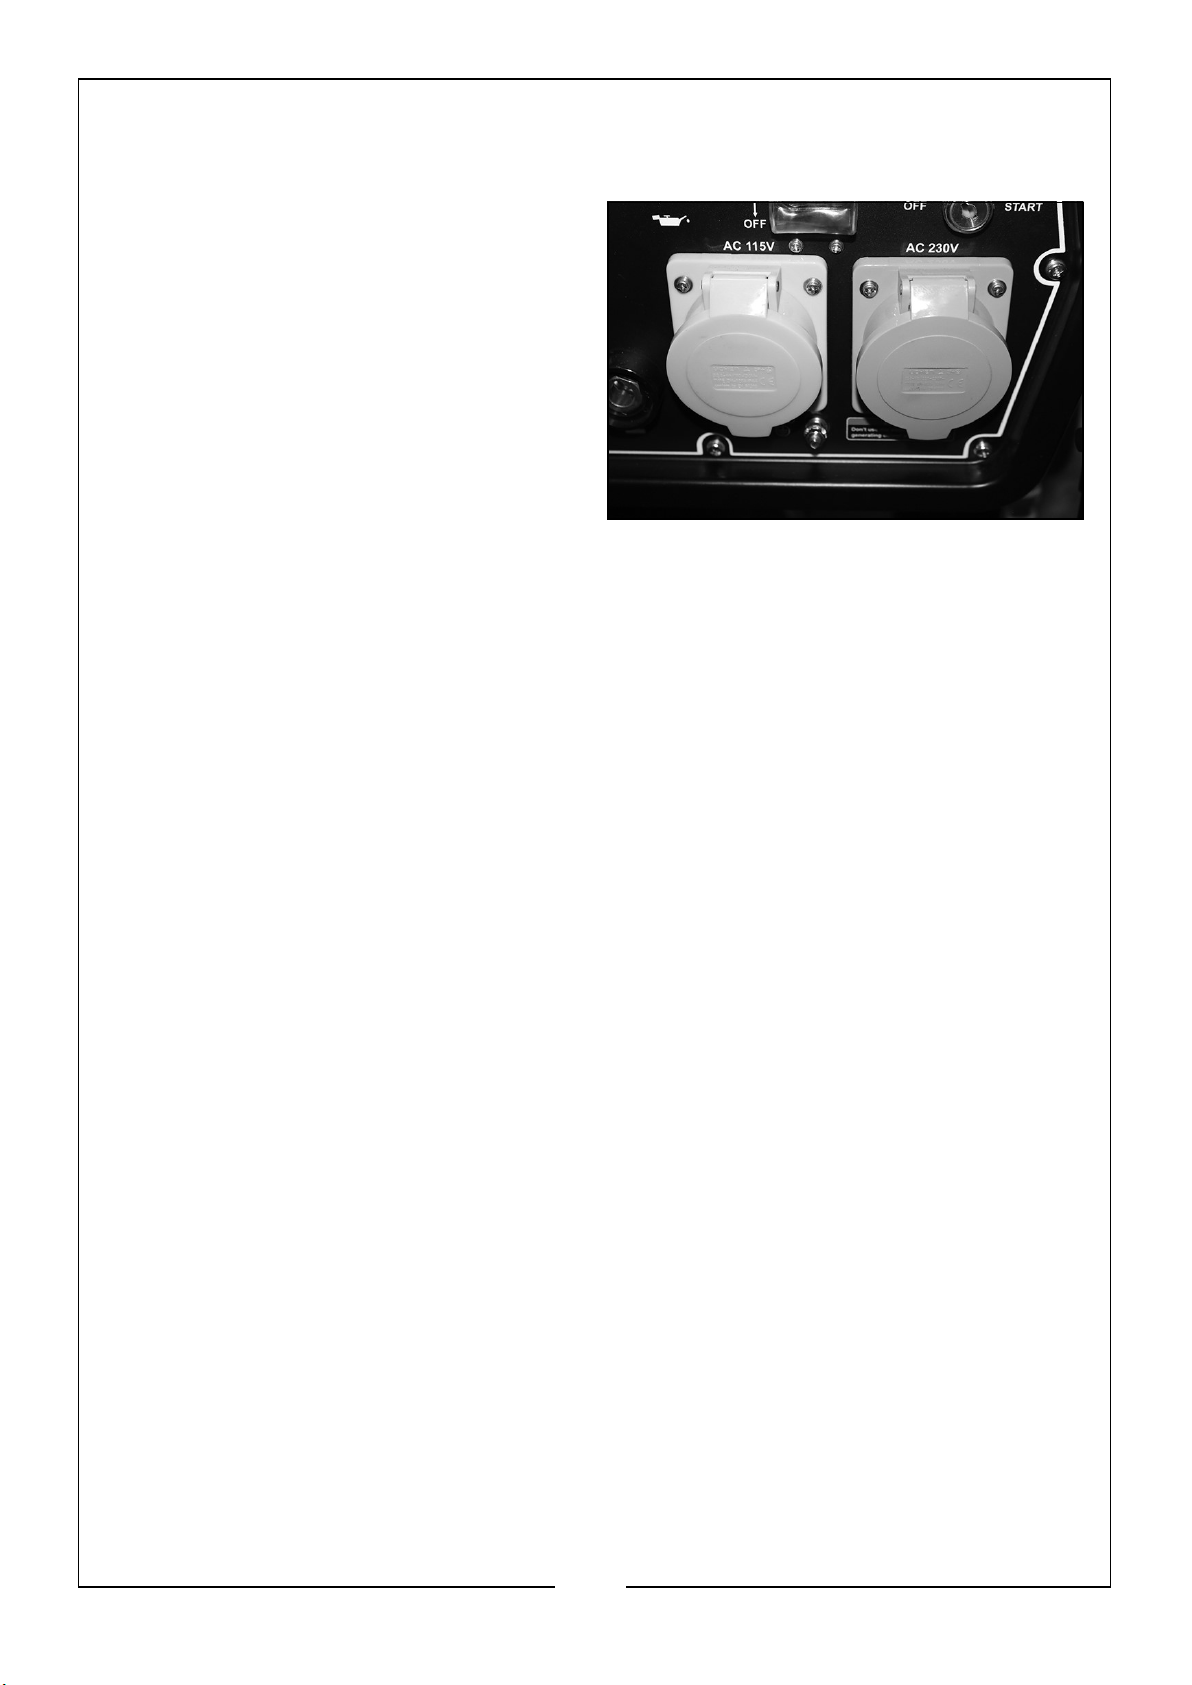
CONNECTING ELECTRICAL DEVICES
The generator can supply both 230V AC and 110V AC.
The sockets are laid out in the following
order: (from left to right):
1. 1 x 16amp 115v (Small Yellow)
2. 1 x 13amp 230V (Small Blue)
Follow the steps below to properly connect your device(s) to the generator.
1. Before connecting electrical devices, allow the generator to run for a few minutes
to stabilise the speed and voltage output.
2. Select the device with the highest wattage and make sure it is turned off. Plug the
device into the generator and then turn the device on. Allow the engine to
stabilise.
3. Repeat step 2 to plug in each additional device. DO NOT attempt to plug in and
start multiple devices at the same time.
GENERATOR CAPACITY
Make sure the generator can supply enough running (rated) and starting (max.) watts
for the items you will power at the same time. Follow these simple steps.
1. Select the items you will power at the same time.
2. Total the running (rated) watts of these items. This is the amount of power the
generator must produce to keep the items running.
3. Estimate how many starting (max.) watts you will need. Starting wattage is the
short burst of power needed to start electric motor driven tools such as a circular
saw or refrigerator. Because not all motors start at the same time, total starting
(max.) watts can be estimated by adding only the items with the highest
additional starting (max.) to the total rated watts.
15
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 16
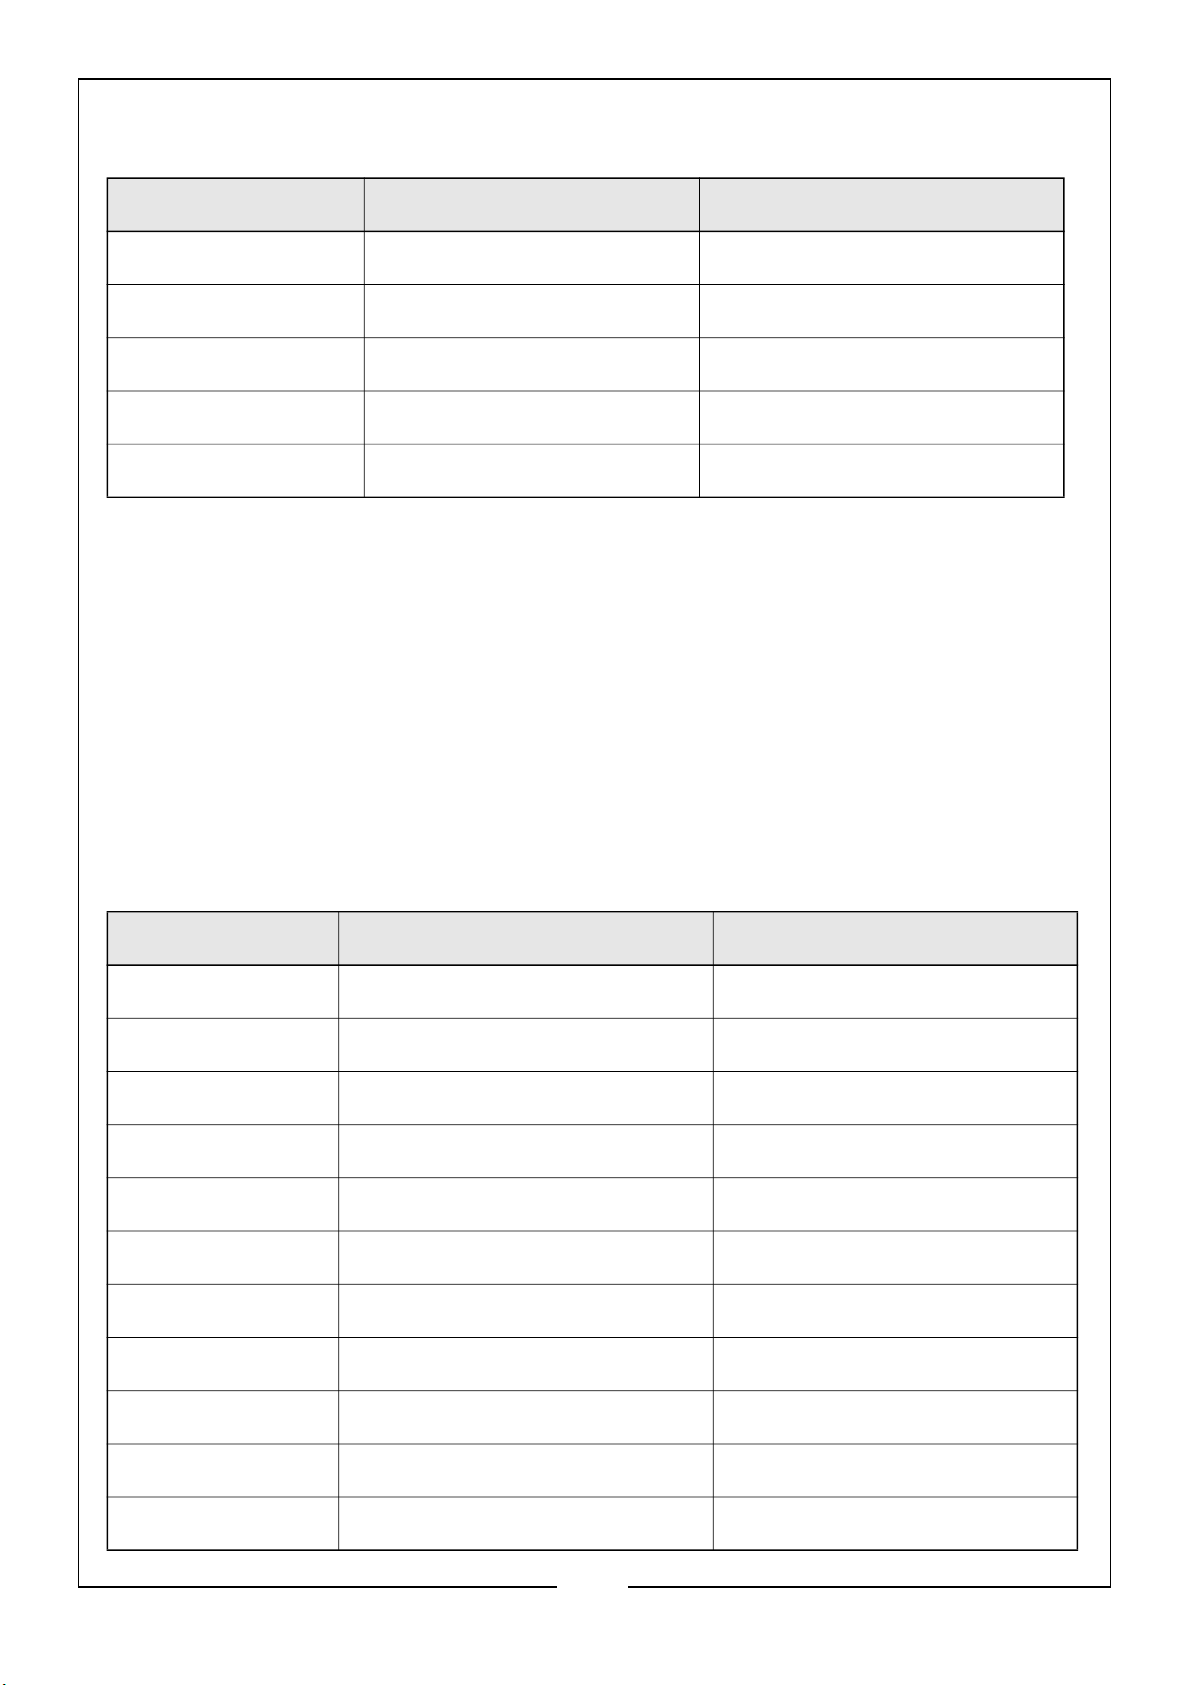
Example:
Tool/Appliance Running Watts Additional Starting Watts
Refrigerator 700 1350
Portable Fan 40 120
Laptop 250 250
46 in. Flat Screen TV 190 190
1180 Total Running Watts 1275 Highest Starting Watts
Total Running Watts: 1180
Highest Starting Watts: +1275
Total Starting Watts Needed = 2455
NEVER add more loads than the generator capacity. Take special care to consider surge
loads in generator capacity as previously described.
The chart below serves as a reference only for the estimated wattage requirements of
common electrical devices. however, DO NOT solely reply on this chart, all electronics
and appliances are built differently, ALWAYS check the wattage listed on the electrical
device before consulting this chart:
Tool/Appliance Rated (Running) Watts Surge (Starting) Watts
Hot Plate 2500 0
Saw - Circular 1500 1500
Saw - Mitre 1200 1200
Microwave 1000 0
Well Water Pump 1000 1000
Sump Pump 800 1200
Refrigerator 800 1200
Computer 800 0
Television 500 0
Box Fan 300 600
Light Bulb 75 0
16
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 17
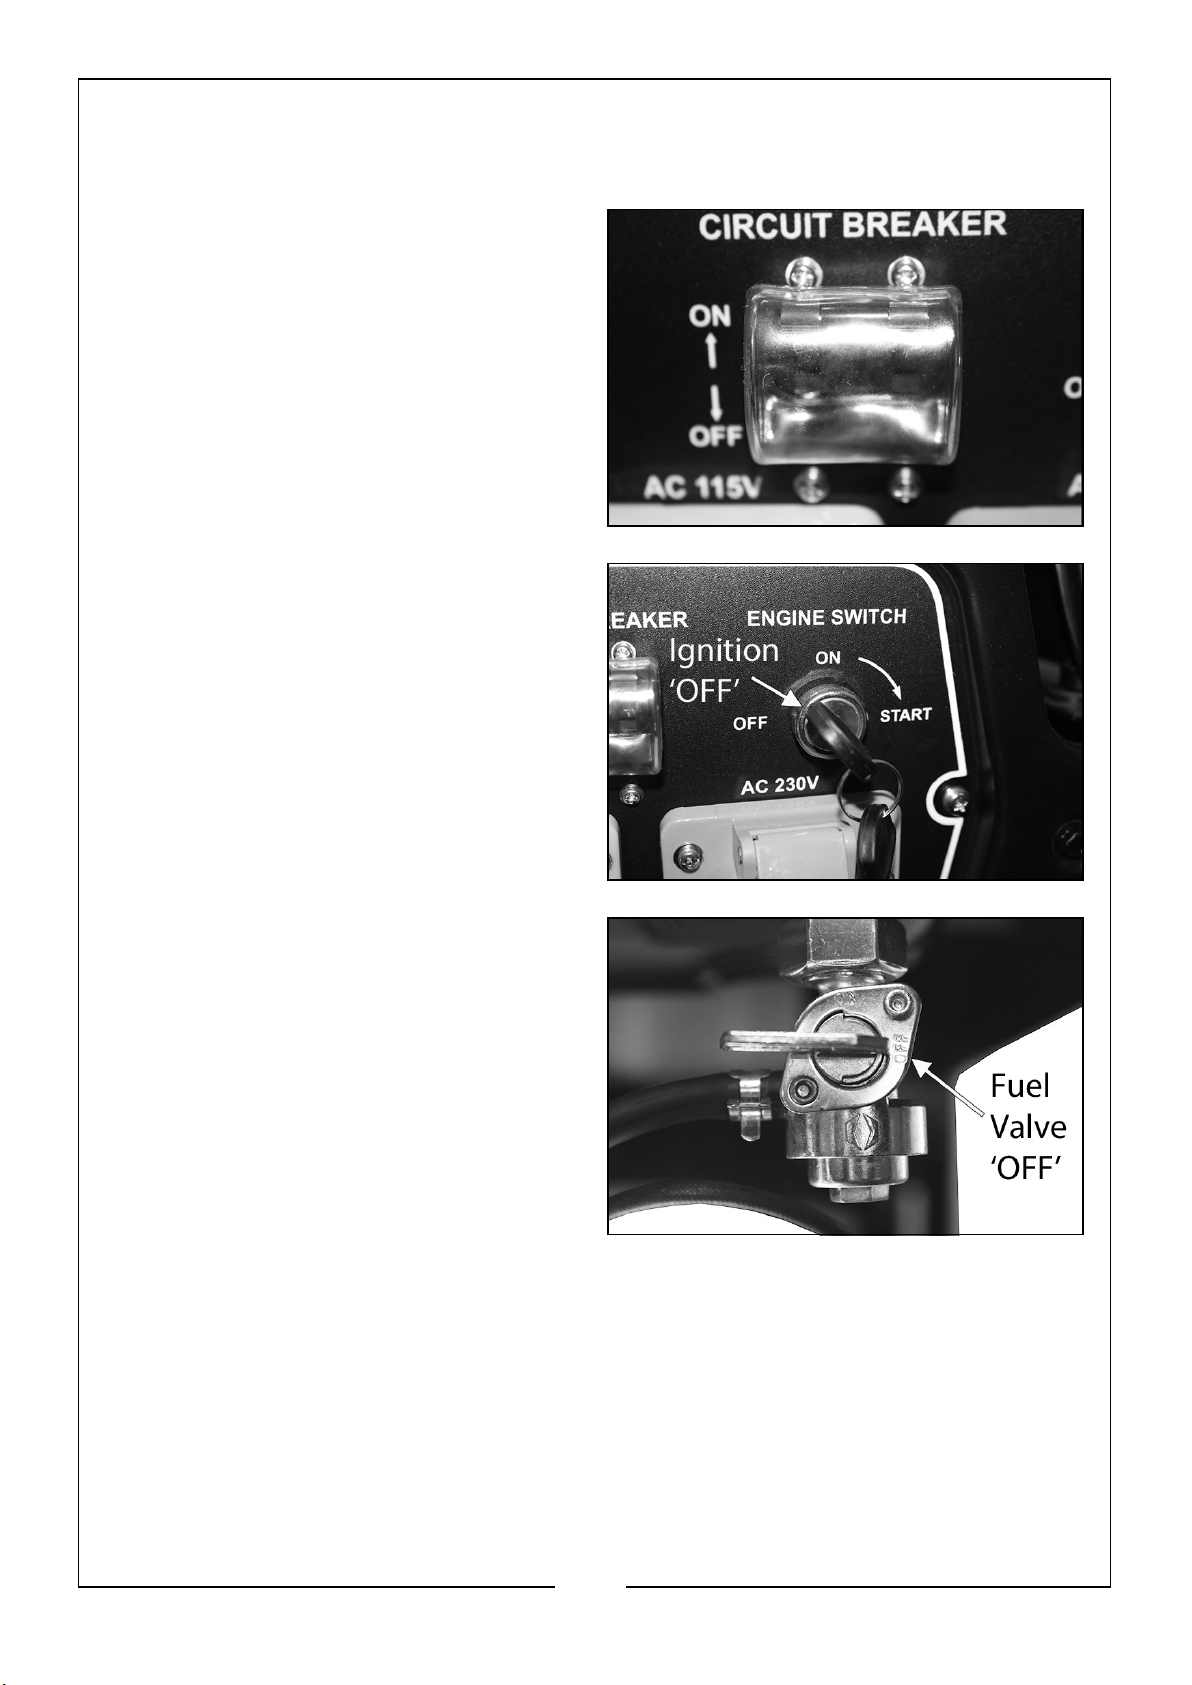
SHUTTING DOWN THE GENERATOR
1. Disconnect all electrical and welding devices.
2. Make sure that the AC breaker is set
to the off (down) position.
3. Turn the ignition key to the ‘OFF’
position.
4. Turn the fuel valve to “OFF”.
NOTE: To stop the generator in an
emergency simply turn the ignition
key to the ‘OFF’ position.
17
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 18
GENERAL SAFETY PRECAUTIONS FOR ALL
TYPES OF WELDING
WARNING: AS WITH ALL MACHINERY, THERE ARE CERTAIN
HAZARDS INVOLVED WITH THEIR OPERATION AND USE.
EXERCISING RESPECT AND CAUTION WILL CONSIDERABLY LESSEN
THE RISK OF PERSONAL INJURY. HOWEVER, IF NORMAL SAFETY
PRECAUTIONS ARE OVERLOOKED, OR IGNORED, PERSONAL INJURY
TO THE OPERATOR MAY RESULT.
FAILURE TO FOLLOW THESE RULES MAY RESULT IN SERIOUS PERSONAL INJURY
GENERAL PRECAUTIONS
A) BURN PREVENTION
Wear protective clothing - gauntlet gloves designed for use in welding, apron, and
protective shoes. Button any shirt collar and pocket flaps, and wear cuffless trousers
to avoid entry of sparks and slag. Wear a helmet with safety goggles or glasses with
side shields underneath, appropriate filter lenses or plates (protected by clear glass).
This is a MUST for welding (and chipping) to protect the eyes from radiant energy and
spatter. Replace cover glass when broken, pitted, or spattered. Avoid oily greasy
clothing. A spark may ignite them. Hot metal should never be handled without gloves.
First aid facilities and a qualified first-aid person should be available unless medical
facilities are close by, for immediate treatment of flash burns of the eyes and skin
burns. Ear plugs should be worn when working overhead or in a confined space. A
hard hat should be worn when others are working overhead. Flammable hair
preparations should not be used by persons intending to weld or cut.
NOTE: ALL protective wear including masks & head shields MUST comply with
PPE Directive 89/686/EEC
B) TOXIC FUME PREVENTION
Severe discomfort, illness or death can result from fumes, vapours, heat, or oxygen
enrichment or depletion that welding (or cutting) may produce. Prevent them with
adequate ventilation. NEVER ventilate with oxygen. Lead-, cadmium-, zinc-, mercuryand beryllium-bearing materials, when welded (or cut) may produce harmful
concentrations of toxic fumes. Adequate local exhaust ventilation must be used, or
each person in the area as well as the operator must wear an air-supplied respirator.
For beryllium, both must be used. Metals coated with or containing materials that
emit toxic fumes should not be heated unless any coating is removed from the work
surface, the area is well ventilated, or the operator wears an air-supplied respirator.
Only work in a confined space when it is being force ventilated and, if necessary,
while wearing an air-supplied respirator. Vapours from chlorinated solvents can be
decomposed by the heat of the arc (or flame) to form PHOSGENE, a highly toxic gas,
and other lung and eye irritating products. The ultraviolet (radiant) energy of the arc
can also decompose trichloroethylene and perchloroethylene vapours to form
18
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 19
phosgene. DO NOT weld or cut where solvent vapours can be drawn into the welding
or cutting atmosphere or where the radiant energy can penetrate to atmospheres
containing even minute amounts of trichloroethylene or perchloroethylene.
C) FIRE AND EXPLOSION PREVENTION
Causes of fire and explosion are:
1. Combustibles reached by the arc, flame, flying sparks, hot slag or heated
material;
2. misuse of compressed gases and cylinders
3. short circuits.
BE AWARE that flying sparks or falling slag can pass through cracks, along pipes,
through windows or doors, and through wall or floor openings, out of sight of the
goggle wearing operator.
To prevent fires and explosion: keep equipment clean and operable, free of oil,
grease, and (in electrical parts) of metallic particles that can cause short circuits. If
combustibles are in the area, DO NOT weld. Move the work if practicable, to an area,
free of combustibles.
Avoid working in paint spray rooms, dip tanks, storage areas, ventilators. If the work
cannot be moved, move any combustibles away from sparks and heat or protect
against ignition with suitable fire- resistant covers or shields.
Walls, ceilings and floors near the work should be protected by heat resistant covers
or shields. A ‘fire watcher’ must be standing by, with suitable fire extinguishing
equipment during, and for some time after welding or cutting if:
1. appreciable combustibles are within 10m.
2. appreciable combustibles are further than 10m but can be ignited by sparks.
3. openings (concealed or visible) in floors or walls can expose combustibles to
sparks.
4. combustibles adjacent to walls, ceilings, roofs or metal partitions can be ignited by
radiant or conducted heat.
After work, check that area is free of sparks, glowing embers and flames. An empty
container that held combustibles or that can produce flammable or toxic vapours
when heated, must never be welded on or cut, unless the container has first been
cleaned. This includes a thorough steam or caustic cleaning (or a solvent or water
washing, depending on the combustible’s solubility) followed by purging and inerting
with nitrogen or carbon dioxide, and using protective equipment.
Water filling just below the working level may substitute for inerting.
A container with unknown contents should be cleaned (see paragraph above). Do
NOT depend on sense of smell or sight to determine if it is safe to weld or cut. Hollow
castings or containers must be vented before welding or cutting - they can explode.
19
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 20
In explosive atmospheres, NEVER weld or cut where the air may contain flammable
dust, gas, or liquid vapours.
ELECTRIC ARC WELDING
Comply with the precautions above and this section. Arc welding, properly done, is a
safe process, but a careless operator invites trouble. The equipment carries high
currents at significant voltages. The arc is very bright and hot. Sparks fly, fumes rise,
ultraviolet and infrared energy radiates and work pieces are hot. The wise operator
avoids unnecessary risks and protects himself and others from accidents.
A) BURN PROTECTION
The welding arc is intense and visibly bright. It’s radiation can damage eyes,
penetrate lightweight clothing, reflect from light coloured surfaces and burn the skin
and eyes. Skin burns resemble acute sunburn, those from gas - shielded arcs are
more severe and painful.
DON’T GET BURNED! FOLLOW ALL SAFETY PRECAUTIONS!
PROTECTIVE CLOTHING
Wear long sleeved clothing (particularly for gas shielded arc) in addition to gloves,
apron and strong shoes. As necessary, use additional protective clothing such as
leather jacket or sleeves, flameproof apron and fire-resistant leggings. Avoid outer
garments of untreated cotton. For bare skin protection wear dark substantial clothing
Keep collars closed to protect the chest and neck and button any pockets to prevent
entry of sparks.
EYE AND HEAD PROTECTION
Protect your eyes from exposure to arc. NEVER look at an electric arc without a
welding helmet or shield containing an appropriate filter plate (Please refer to the
section ‘Welding Shield). Always place over the face before striking an arc. Protect the
filter plate with a clear cover plate. Any cracked or broken helmet or shield should
NOT be worn; radiation can pass through to cause burns.
Cracked, broken, or loose filter plates must be replaced IMMEDIATELY. Replace the
clear cover plate when broken, pitted, or spattered. WE STRONGLY SUGGEST you
wear flash goggles with side shields under the helmet, to give some protection to the
eyes should the helmet not be lowered over the face before an arc is struck. Looking
at an arc momentarily with unprotected eyes (particularly high intensity gas-shielded
arc) can cause a retinal burn that may leave a permanent dark area in the field of
vision. Before welding whilst wearing contact lenses, seek advice from your optician.
PROTECTION OF NEARBY PERSONNEL
For production welding, a separate, well vented room or enclosed bay is best. In open
areas, surround the operation with low reflection, non- combustible screens or panels.
Allow for free air circulation, particularly at floor level. Provide face shields for all
20
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 21
persons who will be looking directly at the weld. Others working in the area should
wear flash goggles. Before starting to weld, make sure that screen or bay doors are
closed.
B) TOXIC FUME PREVENTION
Comply with all precautions in page 3.
C) FIRE AND EXPLOSION PREVENTION
Do not overload arc welding equipment. It may overheat cables and cause a fire.
Loose cable connections may overheat or flash and cause a fire. Never strike an arc
on a cylinder or other pressure vessel. It creates a brittle area that can cause a violent
rupture or lead to such a rupture later under rough handling.
D) SHOCK PREVENTION
Exposed live conductors or other bare metal in the welding circuit, or in unearthed,
electrically-LIVE equipment can fatally shock a person whose body becomes a
conductor. DO NOT STAND, SIT, LIE, LEAN ON, OR TOUCH a wet surface when
welding, without suitable protection.
E) PROTECTION FOR WEARERS OF ELECTRONIC LIFE SUPPORT
DEVICES (PACEMAKERS)
Magnetic fields from high currents can affect pacemaker operation. Persons wearing
pacemakers should consult with their doctor before going near arc welding or spot
welding operations.
F) PROTECTION AGAINST SHOCK
Keep your body and clothing dry. Never work in a damp area without adequate
insulation against electric shock. Stay on a dry duckboard or rubber mat when
dampness or sweat can not be avoided. Sweat, sea water, or moisture between your
body and an electrically LIVE part - or earthed metal - reduces the body surface
electrical resistance, enabling dangerous and possibly lethal currents to flow through
the body.
1) EARTHING THE EQUIPMENT
When arc welding equipment is earthed according to the National Electrical Code and
the workpiece is earthed, a voltage may exist between the electrode and any
conducting object.
Examples of conducting objects include, but are not limited to, buildings, electrical
tools, work benches, welding power source cases, workpieces, etc. Never touch the
electrode and any metal object unless the welding power source is off. When
installing, connect the frames of each unit such as the welding power source, control,
work table and water circulatory to the building earth. Conductors must be adequate
to carry earth currents safely. Equipment made electrically LIVE by stray current may
shock, possibly fatally. Do not EARTH to electrical conduit, or to a pipe carrying ANY
gas or a flammable liquid such as oil or fuel.
21
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 22
2) TORCH
A fully insulated torch should be used without protruding screws or other damage.
3) CONNECTORS
Fully insulated lock-type connectors should be used to join welding cable.
4) CABLES
Frequently inspect cables for wear, cracks and damage. IMMEDIATELY REPLACE those
with excessively worn or damaged insulation to avoid possibly lethal shock from bare
cable. Cables with damaged areas may be taped to give resistance equivalent to
original cable. Keep the cable dry, free of oil and grease and protected from hot metal
and sparks.
5) TERMINALS AND OTHER EXPOSED PARTS
Terminals and other exposed parts of electrical units should have insulating covers
secured before operation.
6) ELECTRODE
a) Equipment with output on/off control (contactor)
Welding power sources for use with the gas metal arc welding, gas tungsten arc
welding and similar processes normally are equipped with devices hat permit on/off
control of the welding power output. When so equipped the electrode wire becomes
electrically LIVE when the power source switch is ON and welding gun switch is
closed. Never touch the electrode wire or any conducting object in contact with the
electrode circuit unless the welding power source is off.
b) Equipment without output on/off control (no contactor)
Welding power sources used with shielded metal arc welding and similar processes
may not be equipped with welding power output on/off control devices. With such
equipment the electrode is electrically LIVE when the power switch is turned ON.
Never touch the electrode unless the welding power source is off.
7) SAFETY DEVICES
Safety devices such as interlocks and circuit breakers should not be disconnected or
shunted out. Before installation, inspection, or service of equipment, shut OFF all
power and remove line fuses (or lock or red-tag switches) to prevent accidental
turning ON of power. Do not open power circuit or change polarity while welding. If,
in an emergency, it must be disconnected, guard against shock burns or flash from
switch arcing. Always shut OFF and disconnect all power to equipment. A power
disconnect switch must be available near the welding power source.
22
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 23
ELECTROMAGNETIC INTERFERENCE (EMC)
Whilst this unit complies with EMC regulations, the user is responsible for installing
and using the welding equipment according to the manufacturers instructions. If
electromagnetic disturbances are detected then it shall be the responsibility of the
user of the welding equipment to resolve the situation. In some cases this remedial
action may be as simple as earthing the welding circuit, see ‘Note’. In other cases it
could involve constructing an electromagnetic screen enclosing the power source and
the work complete with associated input filters. In all cases electromagnetic
disturbances must be reduced to the point where they are no longer troublesome.
NOTE:
The welding circuit may or may not be earthed for safety
reasons. Changing the earthing arrangements should only be
authorised by a person who is competent to assess whether
the changes will increase the risk of injury, e.g. by allowing
parallel welding current return paths which may damage the
earth circuits of other equipment.
ASSESSMENT OF THE AREA
Before installing welding equipment the user shall make an assessment of potential
electromagnetic problems in the surrounding area. Avoid using your inverter in the
vicinity of:
• other supply cables, control cables, signaling and telephone cables; above, below
and adjacent to the welding equipment;
• radio and television transmitters and receivers;
• computer and other control equipment;
• safety critical equipment, e.g. guarding of industrial equipment;
• pacemakers and hearing aids etc;
• equipment used for calibration or measurement;
• other equipment in the environment. The user shall ensure that other equipment
being used in the environment is compatible. This may require additional
protection measures;
It may be possible to avoid the above by changing the time of day that welding or
other activities are to be carried out.
The size of the surrounding area to be considered will depend on the structure of the
building and other activities that are taking place. The surrounding area may extend
beyond the boundaries of the premises.
23
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 24
METHODS OF REDUCING EMISSIONS
MAINS SUPPLY
Welding equipment should be connected to the mains supply according to the
manufacturers recommendations. If interference occurs, it may be necessary to take
additional precautions such as filtering of the mains supply. Consideration should be
given to shielding the supply cable of permanently installed welding equipment, in
metallic conduit or equivalent. Shielding should be electrically continuous throughout
its length. The shielding should be connected to the welding power source so that
good electrical contact is maintained between the conduit and the welding power
source enclosure.
MAINTENANCE OF THE WELDING EQUIPMENT
The welding equipment should be routinely maintained according to the
manufacturers recommendations. All access and service doors and covers should be
closed and properly fastened when the welding equipment is in operation. The
welding equipment should not be modified in any way except for those changes and
adjustments covered in the manufacturers instructions. In particular, the spark gaps
of arc striking and stabilizing devices should be adjusted and maintained according to
the manufacturers recommendations.
WELDING CABLES
The welding cables should be kept as short as possible and should be positioned close
together, running at or close to the floor level.
EQUIPOTENTIAL BONDING
Bonding of all metallic components in the welding installation and adjacent to it
should be considered. However, metallic components bonded to the work piece will
increase the risk that the operator could receive a shock by touching these metallic
components and the electrodes at the same time. The operator should be insulated
from all such bonded metallic components.
EARTHING OF THE WORKPIECE
Where the workpiece is not bonded to earth for electrical safety, nor connected to
earth because of its size and position, e.g. a ships hull or building steelwork, a
connection bonding the workpiece to earth may reduce emissions in some, but not all
instances.
Care should be taken to prevent the earthing of the workpiece increasing the risk of
injury to users, or damage to other electrical equipment.
Where necessary, the connection of the workpiece to earth should be made by a
direct connection to the workpiece, but in some countries where direct connection is
not permitted, the bonding should be achieved by suitable capacitance, selected
according to national regulations.
24
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 25
SCREENING AND SHIELDING
Selective screening and shielding of other cables and equipment in the surrounding
area may alleviate problems of interference. Screening of the entire welding
installation may be considered for special applications.
OPERATION - WELDING
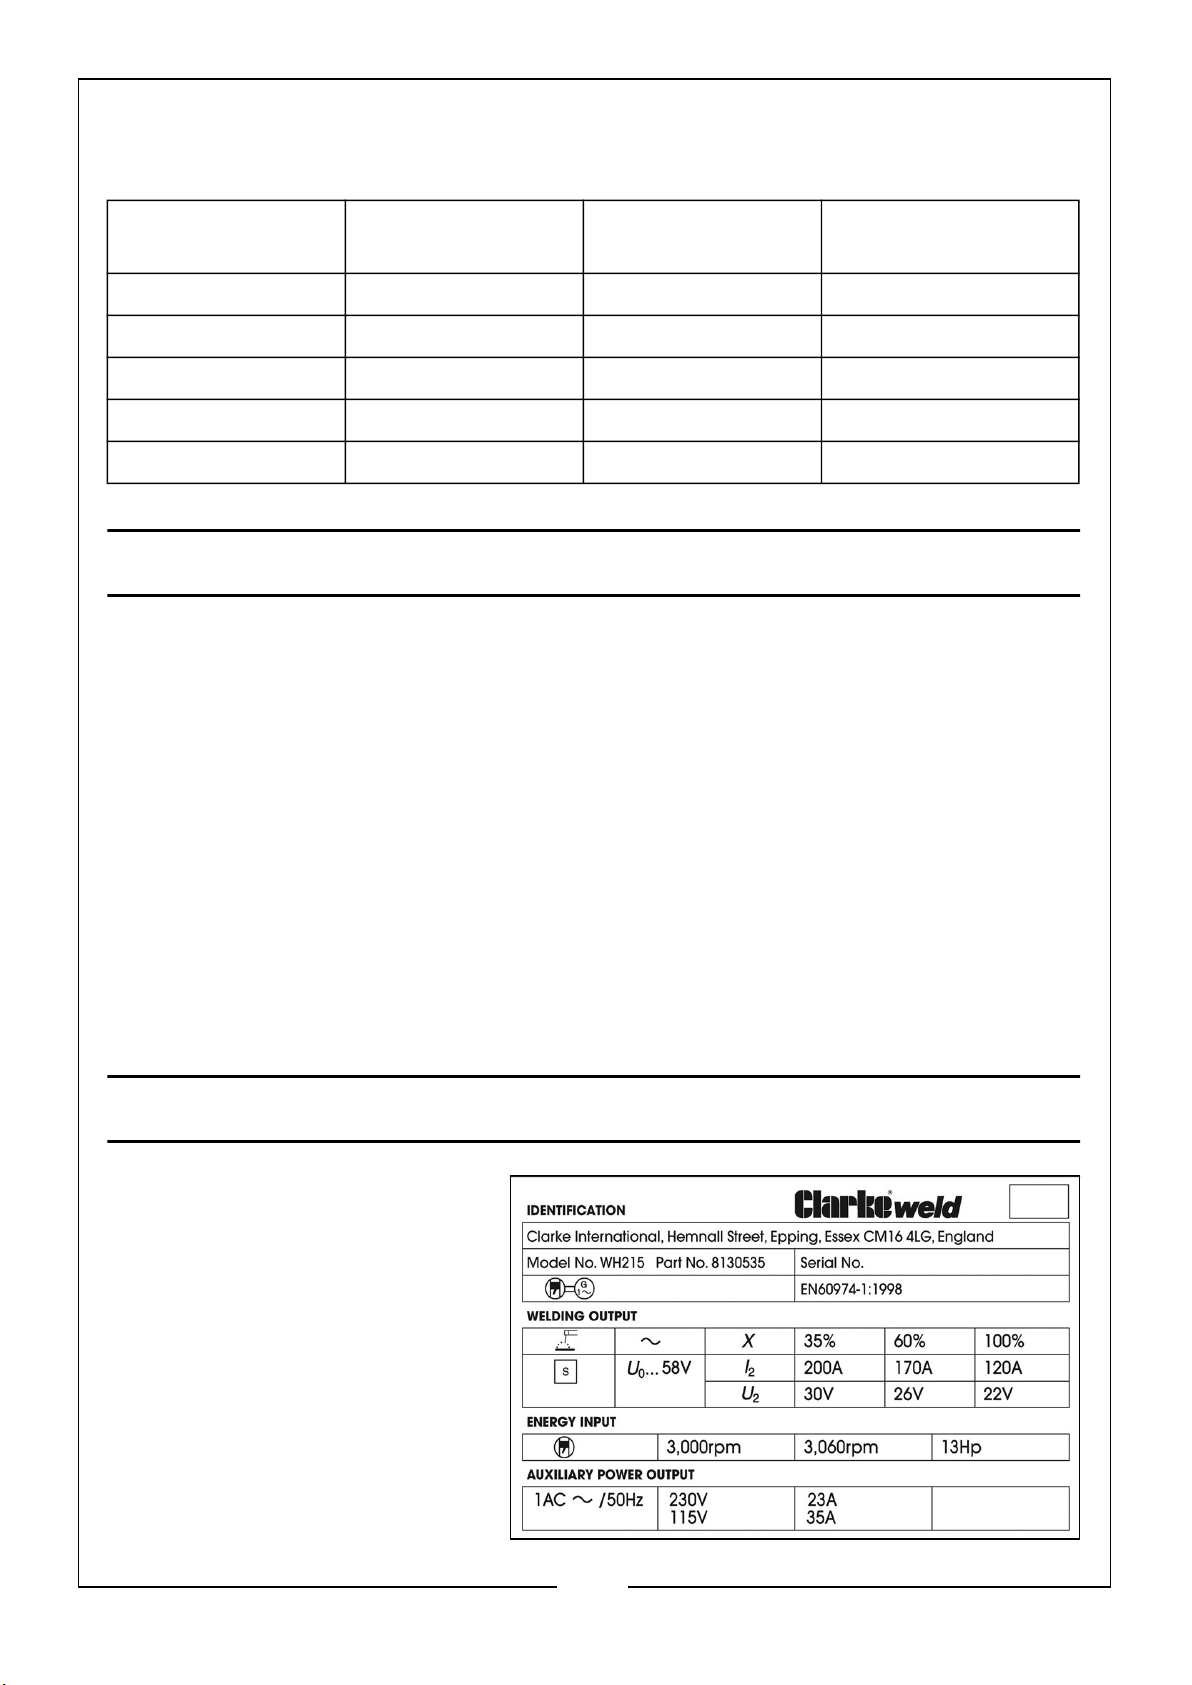
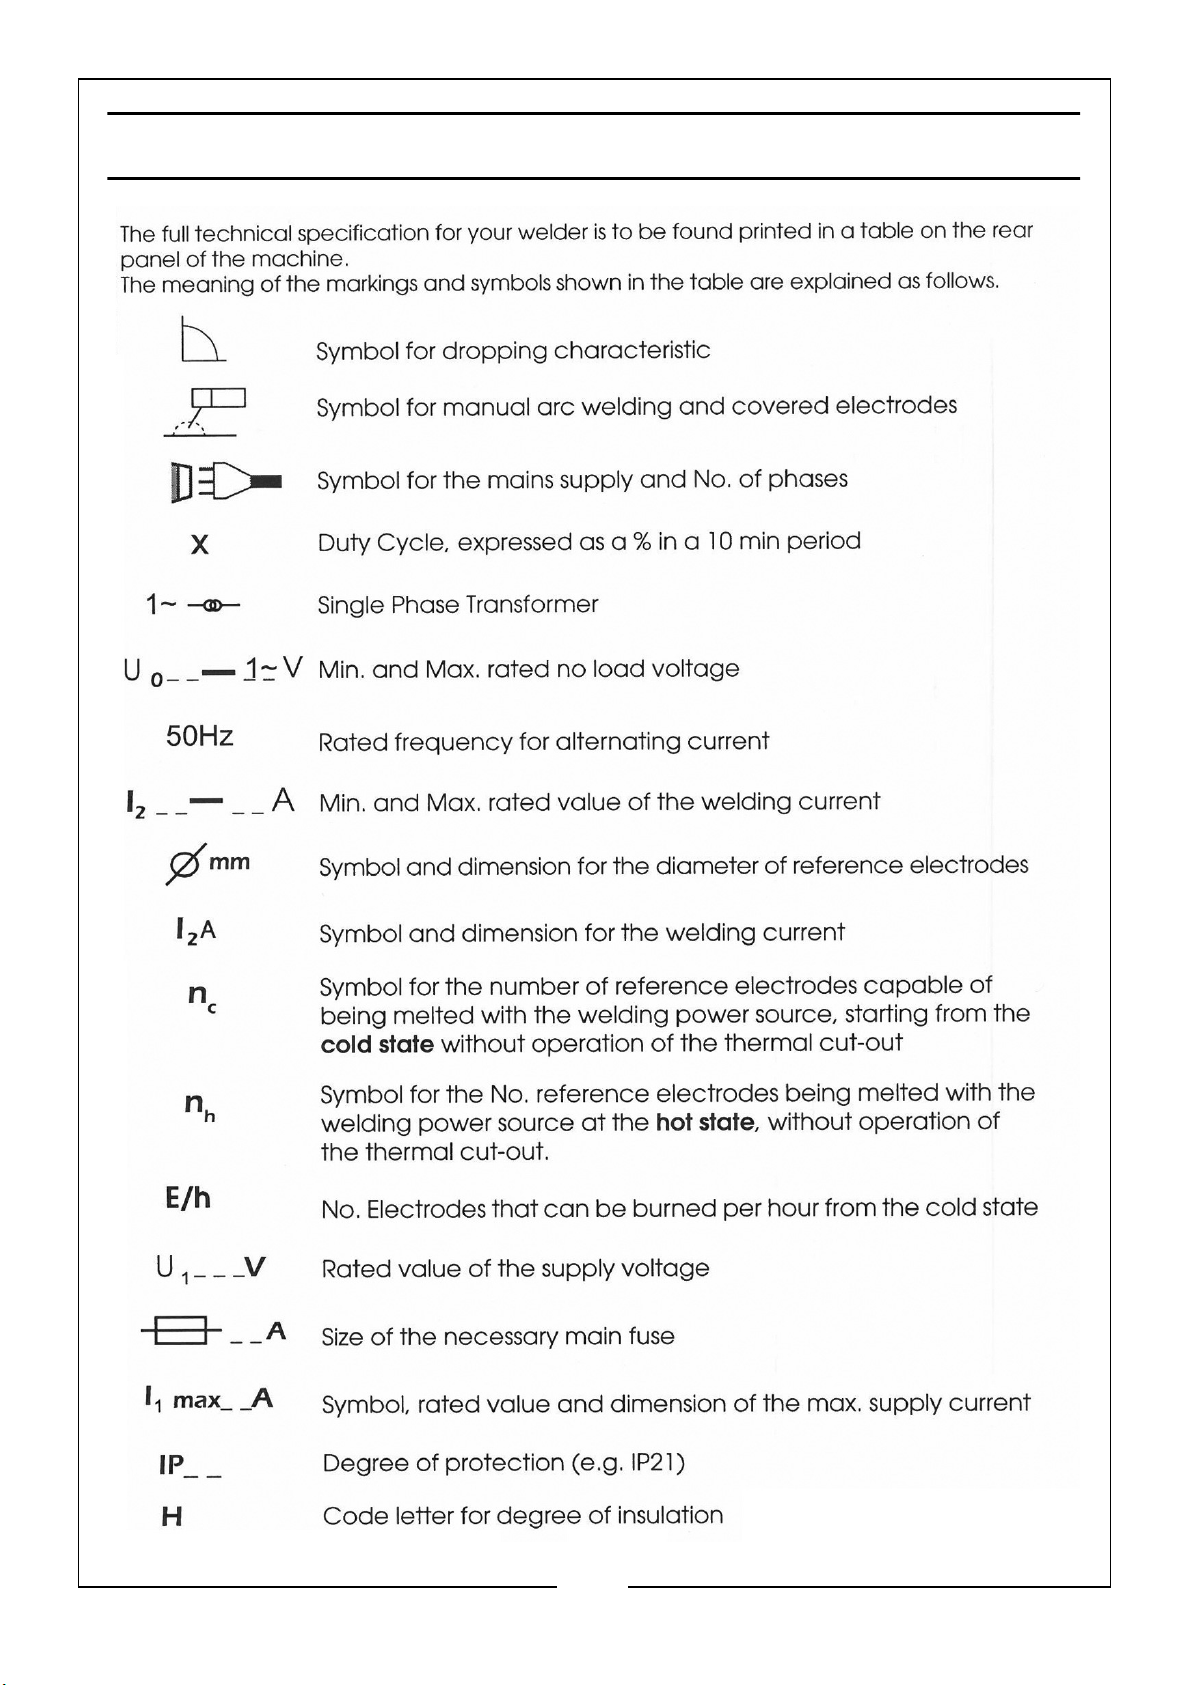
The welding capabilities of your welder are given on the data label printed on the rear
panel of the machine, and reproduced on page 16. An explanation of markings and
symbols appearing on the data label is shown on page 21.
THERMAL OVERLOAD PROTECTION
If the duty cycle of the welder is exceeded (see Specifications), the Overload
Protection Device will automatically cut the power to prevent damage to the machine.
Should the cut-out operate, you will have to wait until the transformer cools down
(approx. 30 minutes), when the overload device will automatically reset itself.
Although no harm will be done to the machine if/when the overload device is
actuated, its frequent use could eventually result in damage.
PREPARATION FOR WELDING
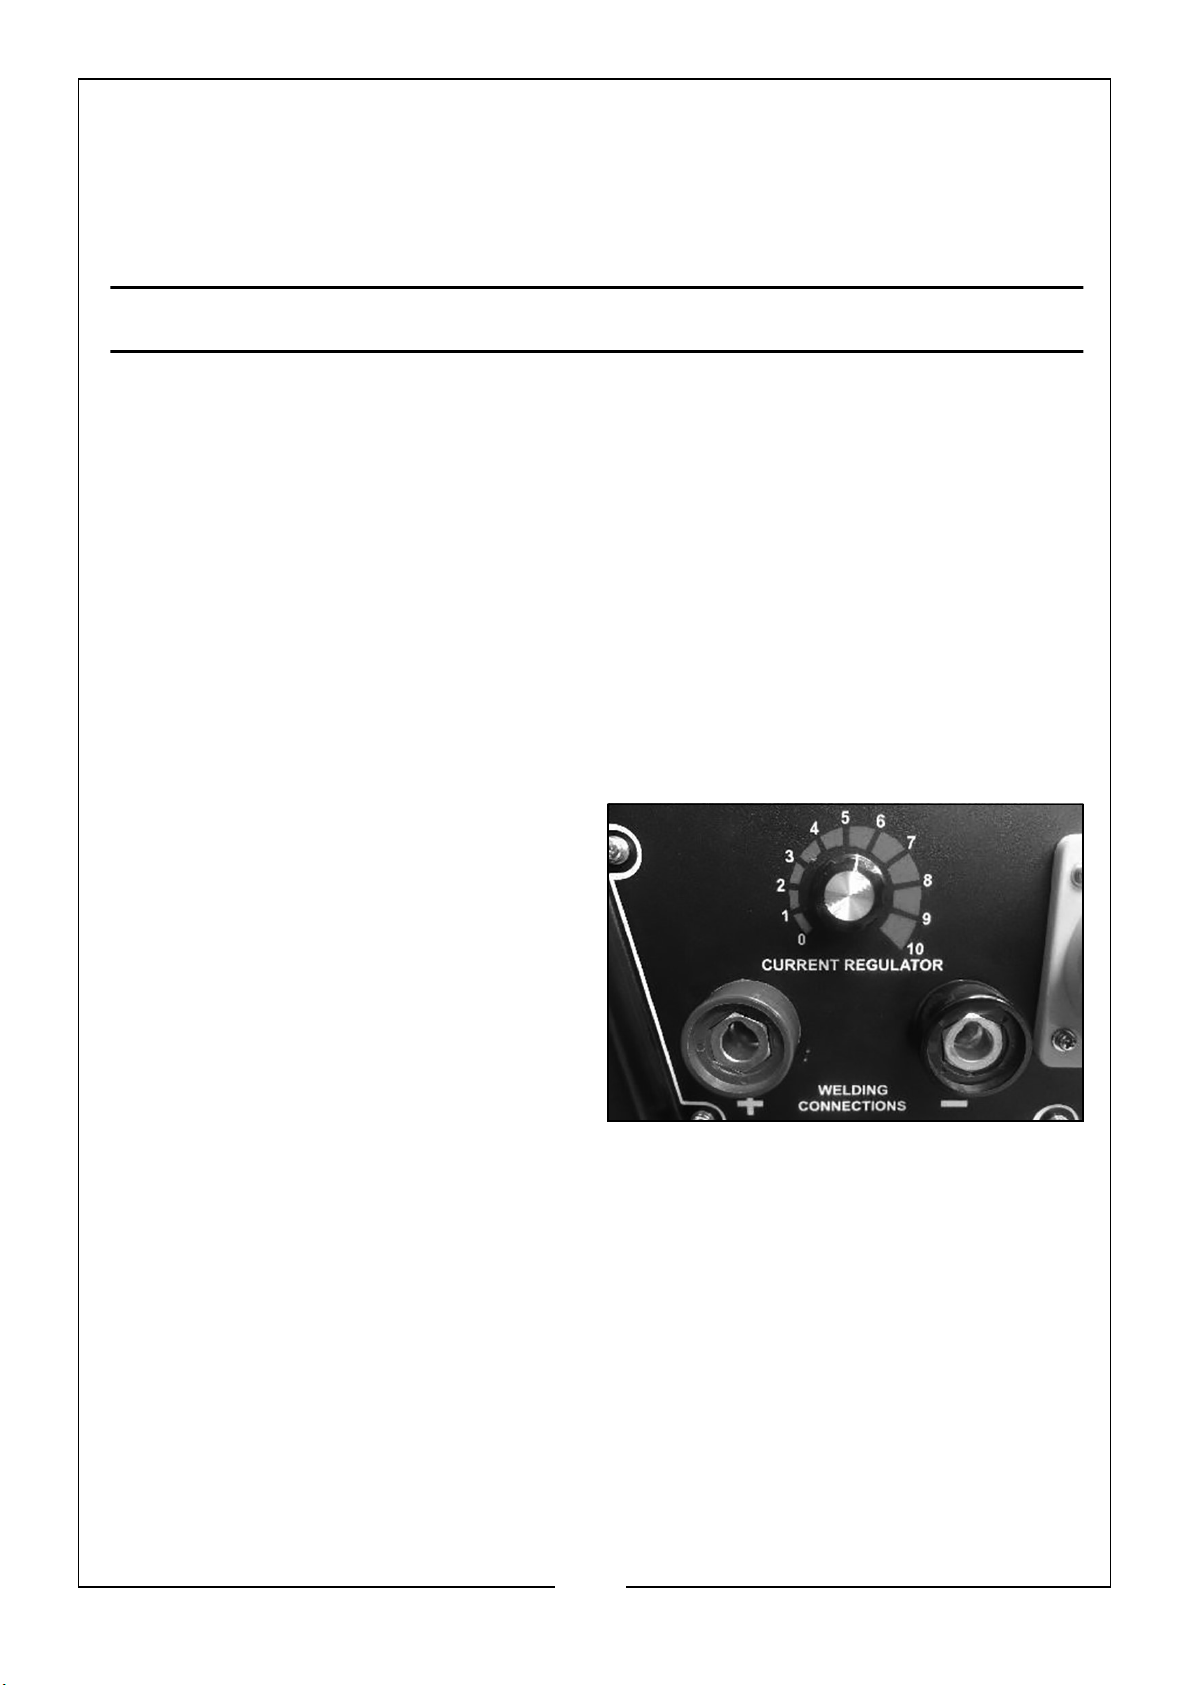
1. Connect the red welding lead to the
appropriate DIN socket (RED, +).
2. Connect the black earth clamp lead
to the COM DIN socket (BLACK, -).
3. Make sure that the two welding lead
ends DO NOT touch while connected
to the welder.
4. Ensure the earth clamp is connected
to the work piece.
IMPORTANT: Ensure also that the earth clamp is attached to clean, solid
metal. If necessary thoroughly clean with a wire brush or similar to
guarantee a good connection.
5. Select the appropriate electrode (see page 26 for a full list of CLARKE electrodes),
which should be approximately the same thickness as the piece to be welded, for
single pass welding.
NOTE:
With practice you will get a feel for the best current settings
for different welding rod thicknesses.
6. Adjust the Current Regulator to the required level
7. Turn the generator engine on, see pages 13 - 14.
8. To turn the generator engine off, see page 17.
25
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 26
The chart below gives an indication of the thickness of material/welding rod thickness
and the corresponding welding current. This is intended as a guide only.
Work Piece
Thickness
Up-to 2mm 1.6mm - 2.5mm 40A - 60A 1 - 2
3mm 2.5mm - 3.2mm 60A - 80A 3 - 4
4mm - 5mm 3.2mm - 4mm 90A - 130A 5 -6
6mm - 12mm 4mm - 5mm 160A - 210A 7 - 8
Above 13mm 5mm - 6mm 200A - 270A 9 - 10
Welding Rod
Diameter
Welding Current Current Regulator
Setting
CLARKE ELECTRODES
• 1.6mm x 300mm E6013 Welding Electrodes, 5kg Bulk Pack; Part No: 3050590
• 2.0mm x 300mm E6013 Welding Electrodes, 5kg Bulk Pack; Part No: 3050592
• 2.5mm x 350mm E6013 Welding Electrodes, 5kg Bulk Pack; Part No: 3050594
• 3.25mm x 350mm E6013 Welding Electrodes, 5kg Bulk Pack; Part No: 3050596
• 4.0mm x 400mm E6013 Welding Electrodes, 5kg Bulk Pack; Part No: 3050598
• 1.6mm WC20 Grey Tungsten Welding Electrodes, 10 Pack; Part No: 3050630
• 1.6mm WL20 Sky Blue Tungsten Welding Electrodes, 10 Pack; Part No: 3050640
• 2.4mm WC20 Grey Tungsten Welding Electrodes, 10 Pack; Part No: 3050635
• 2.4mm WL20 Sky Blue Tungsten Welding Electrodes, 10 Pack; Part No: 3050645
DUTY CYCLES
This model is covered by
regulations EN 60974-1 and EN
50199, where the Duty Cycle (X)
is expressed as a percentage of
time the machine may be used
in a given period for a specified
welding current.
i.e. using the example shown:
26
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 27
When welding at 170 Amps the machine may be used for 6 minutes (60%)
in any 10 minute period, or, the machine may be used continuously,
(100%) when welding at 120 Amps.
WELDING TECHNIQUE
1. With the welder correctly connected to the mains supply and the leads attached to
the machine, ensure the earth clamp is firmly attached to the workpiece on
CLEAN, SOLID metal and as close to the proposed weld as is practical, and the
appropriate current setting for the job has been set.
2. Start the engine.
NOTE:
If the machine stops at any time and the amber light on the
front panel illuminates, the thermal cutout has intervened.
Wait until the transformer has cooled sufficiently for work to
recommence. This could take considerable time and is denoted
by the amber light going OUT.
3. Bring the electrode to the work surface at an angle of approx 70o then, BEFORE
you strike an arc, bring the face shield up to protect your eyes.
Strike an arc by briefly touching the work surface with the tip of the electrode. Once
the arc is struck or primed, raise the electrode slightly and maintain it at a distance of
approx 1.5mm (1/16”) from the work surface, then proceed to move the electrode
along its intended path, keeping the tip in the molten pool at all times. An even
crackling noise should be heard, which is an indication of a good weld.
NOTE: This is the most difficult aspect for most beginners. It is
recommended that you practice on some scrap material in
order to get a feel of the operation.
If the electrode is not withdrawn quickly enough once the arc is primed,
there is a possibility that the electrode will weld itself to the workpiece.
Should this happen, give it a sharp tug to free it and try again. If this fails
to free it, turn OFF the machine immediately as it will quickly overheat.If
you withdraw the electrode too far once the arc is primed, you will lose the
arc and have to try again.
4. Inspect the job carefully. With a correct combination of electrode size and current
setting the area of weld should be complete fusion of the electrode and parent
metal/s. Any slag which forms on the surface should be chipped away with a pick/
brush.
If the resultant weld looks messy and irregular, this is an indication of porosity or slag
contamination and you have almost certainly failed to achieve the correct
combination. This is a common problem, so do not worry as practice will quickly cure
this.
27
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 28
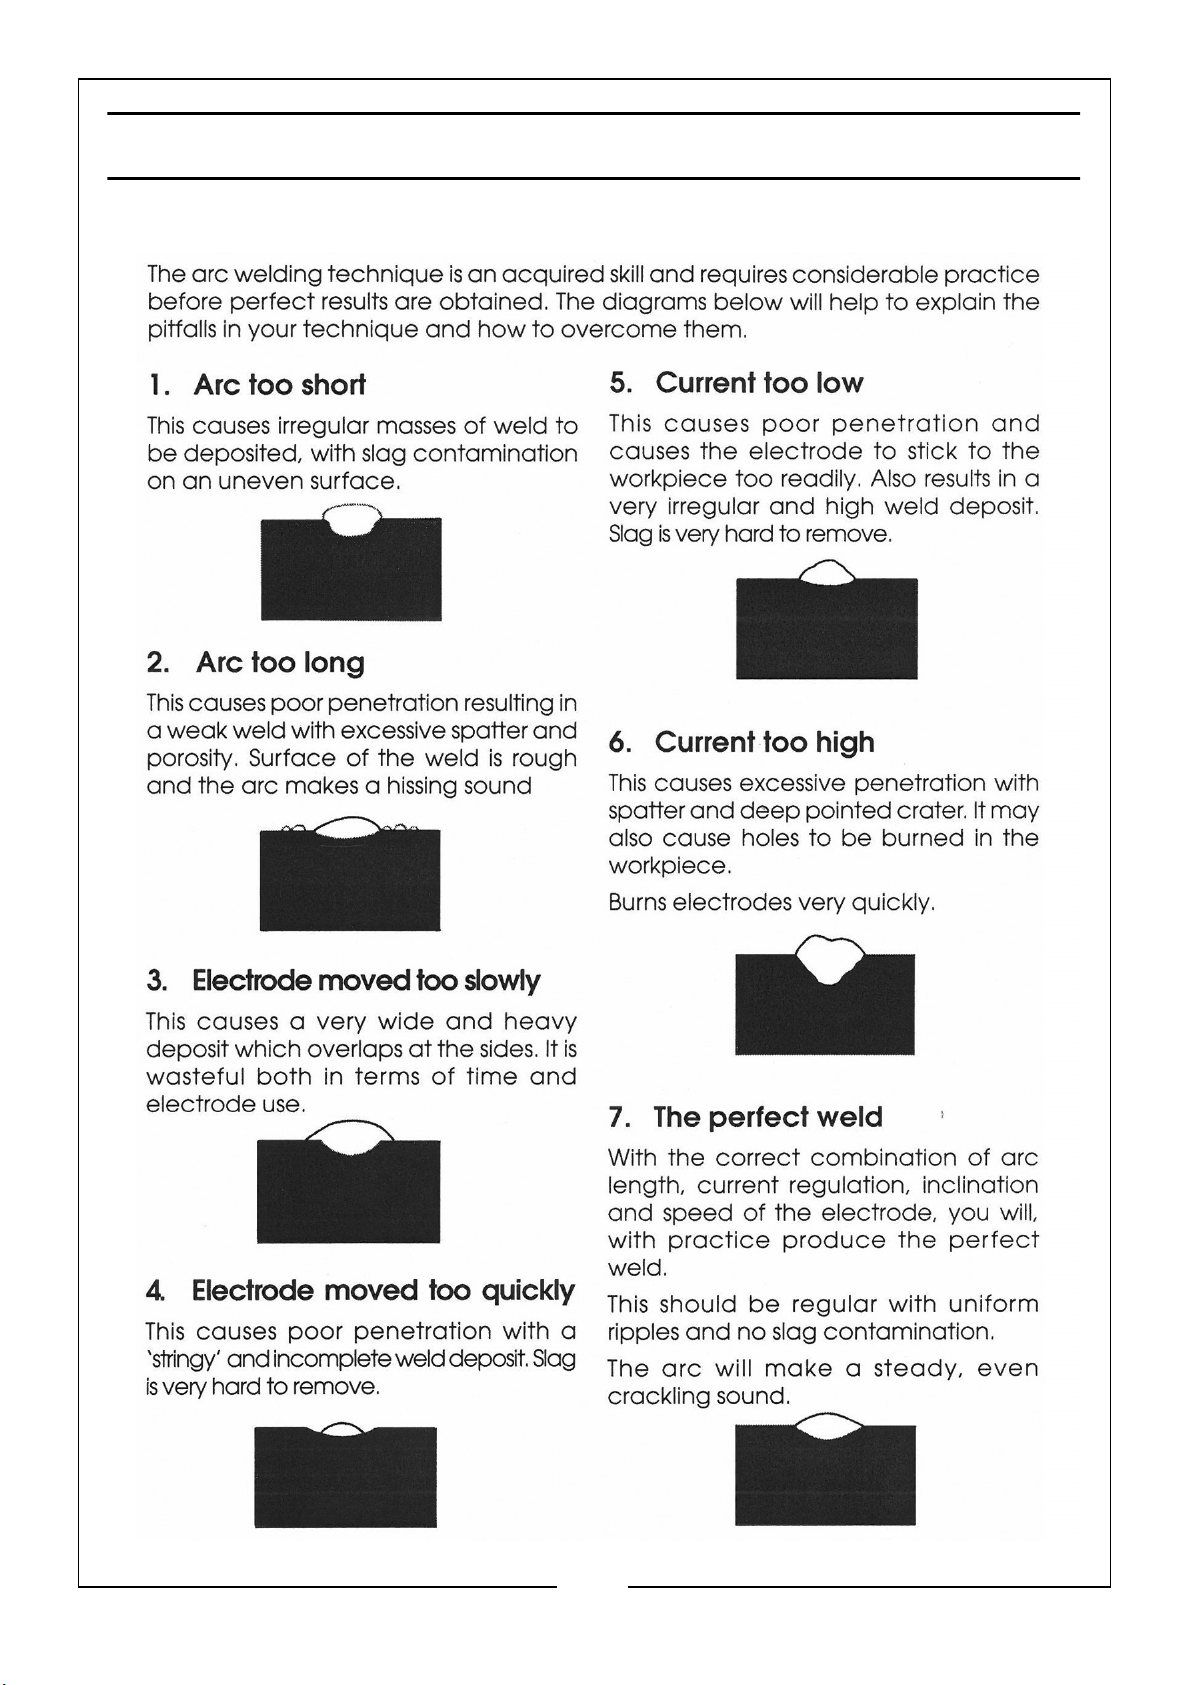
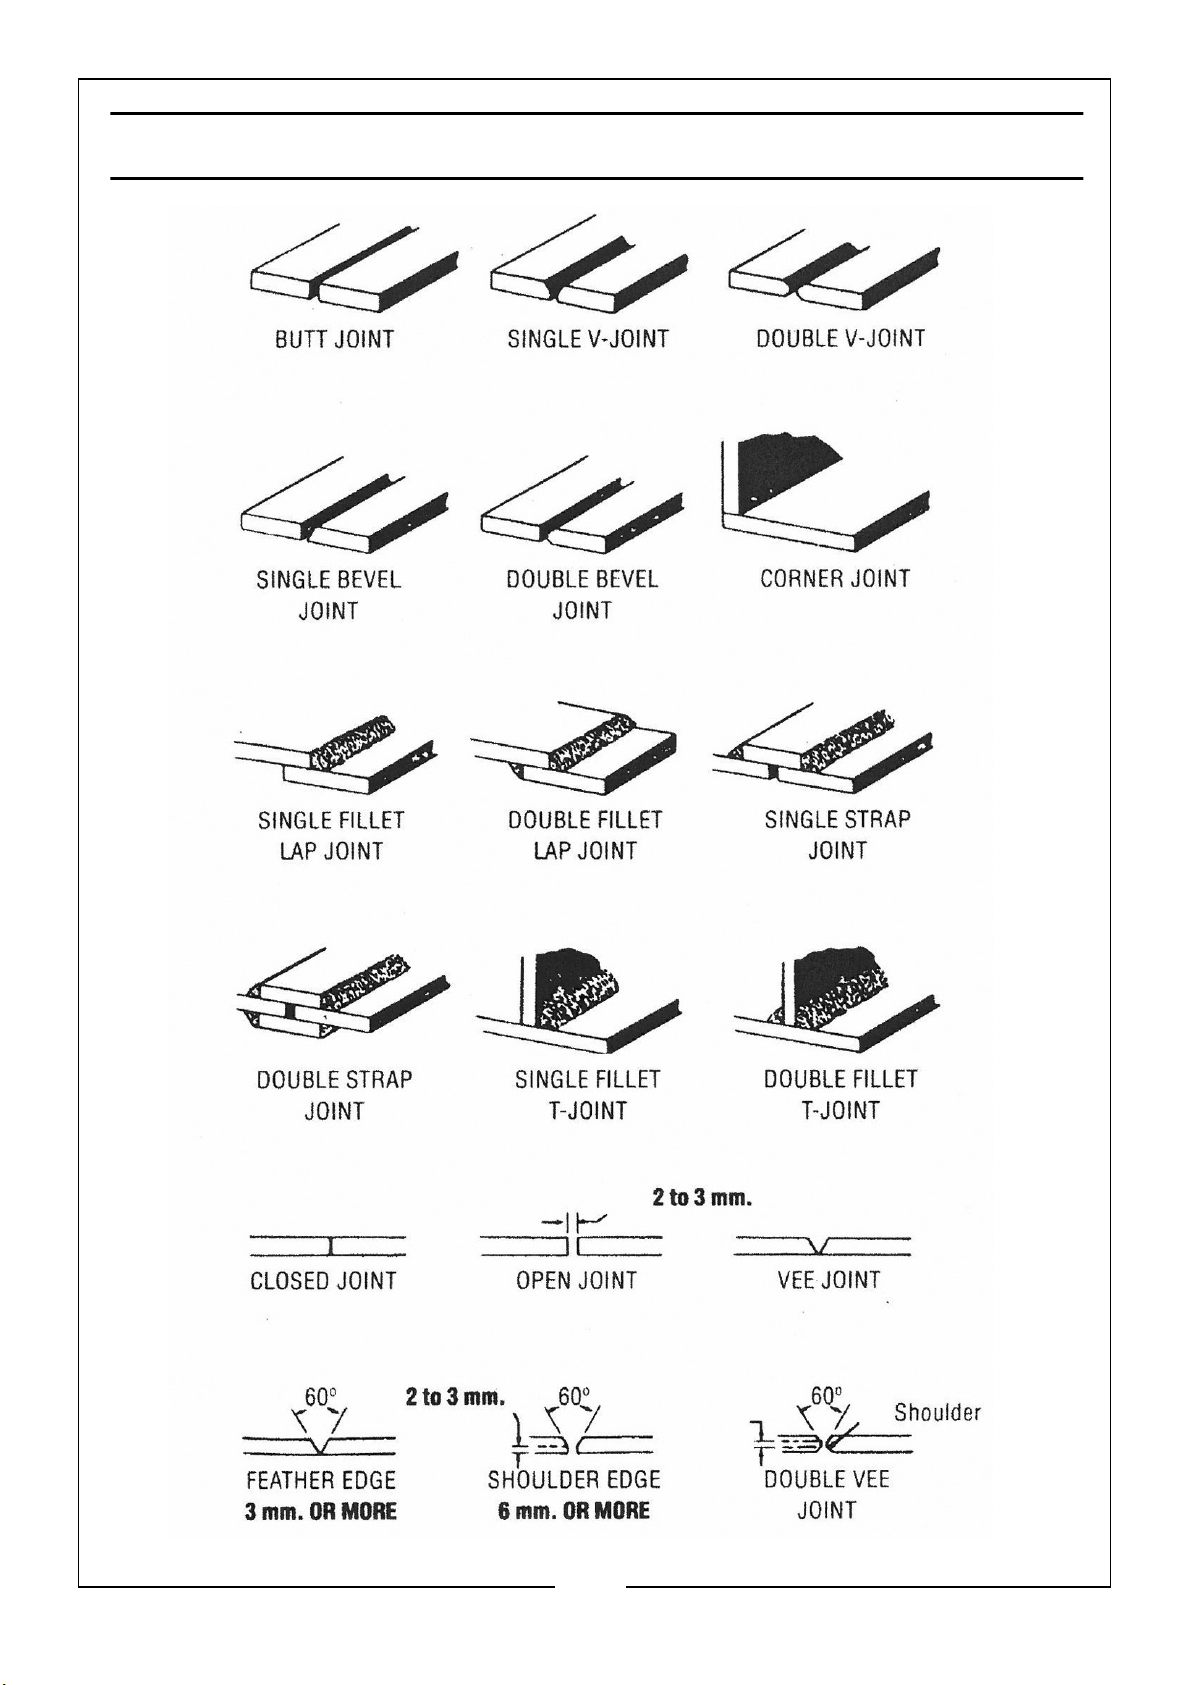
WELDING MISTAKES
The following tips should help you improve your welding technique fairly quickly.
28
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 29
Page 30
ELECTRICAL WELDING SYMBOLS EXPLAINED
30
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 31
MAINTENANCE
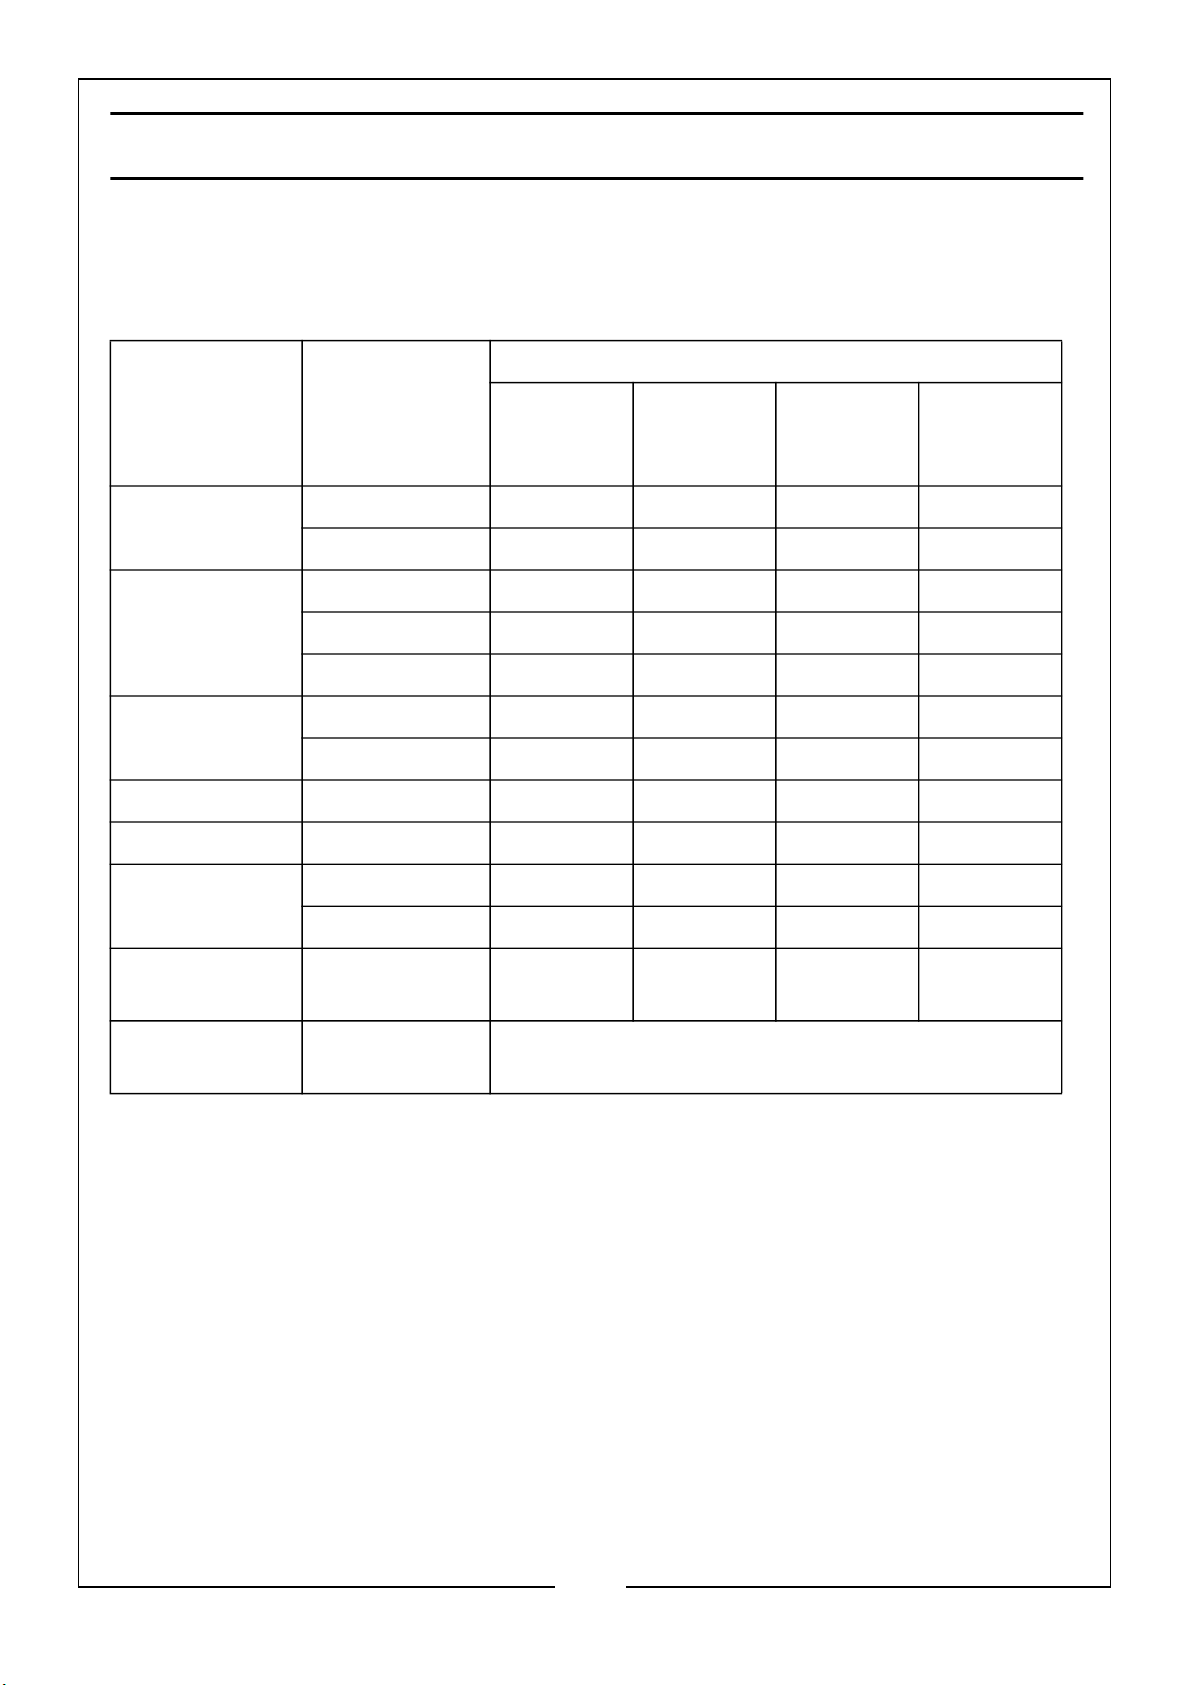
Some adjustments will need to be made periodically to properly maintain the pressure
washer. All service and adjustments should be made at least one time each season. It
is important that the maintenance chart below is followed:
Frequency
Item Action
Engine Oil
(Page 10 & 32)
Air Filter
(Page 34)
Spark Plug
(Page 33)
Idling Check - Adjust ***
Valve Clearance Check - Adjust ***
Fuel Tank
(Page 11 & 35)
Fuel Filter
(Page 11-12)
Check Level *
Replace *
Check *
Clean **
Replace *
Clean - Adjust ****
Replace *
Check Level *
Clean ***
Check - Clean *
Each Time
of Use
Every 3
Months or
50 Hrs
Every 6
Months or
100 Hrs
Every Year
or 300 Hrs
Fuel Supply
Line
• ** = Recommended to be performed more often than in the schedule if
operated in a dusty environment.
• *** = Recommended to be performed by a CLARKE service centre as part of a
full service.
• **** = Adjust air gap to 0.6 - 0.7 mm, see page 33
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Check Every Two Years (Replace if Necessary***)
31
Page 32
CHANGING THE ENGINE OIL
CAUTION: PROLONGED EXPOSURE TO USED ENGINE OIL IS HARMFUL,
ALWAYS WASH YOUR HANDS THOROUGHLY AFTER HANDLING USED
ENGINE OIL.
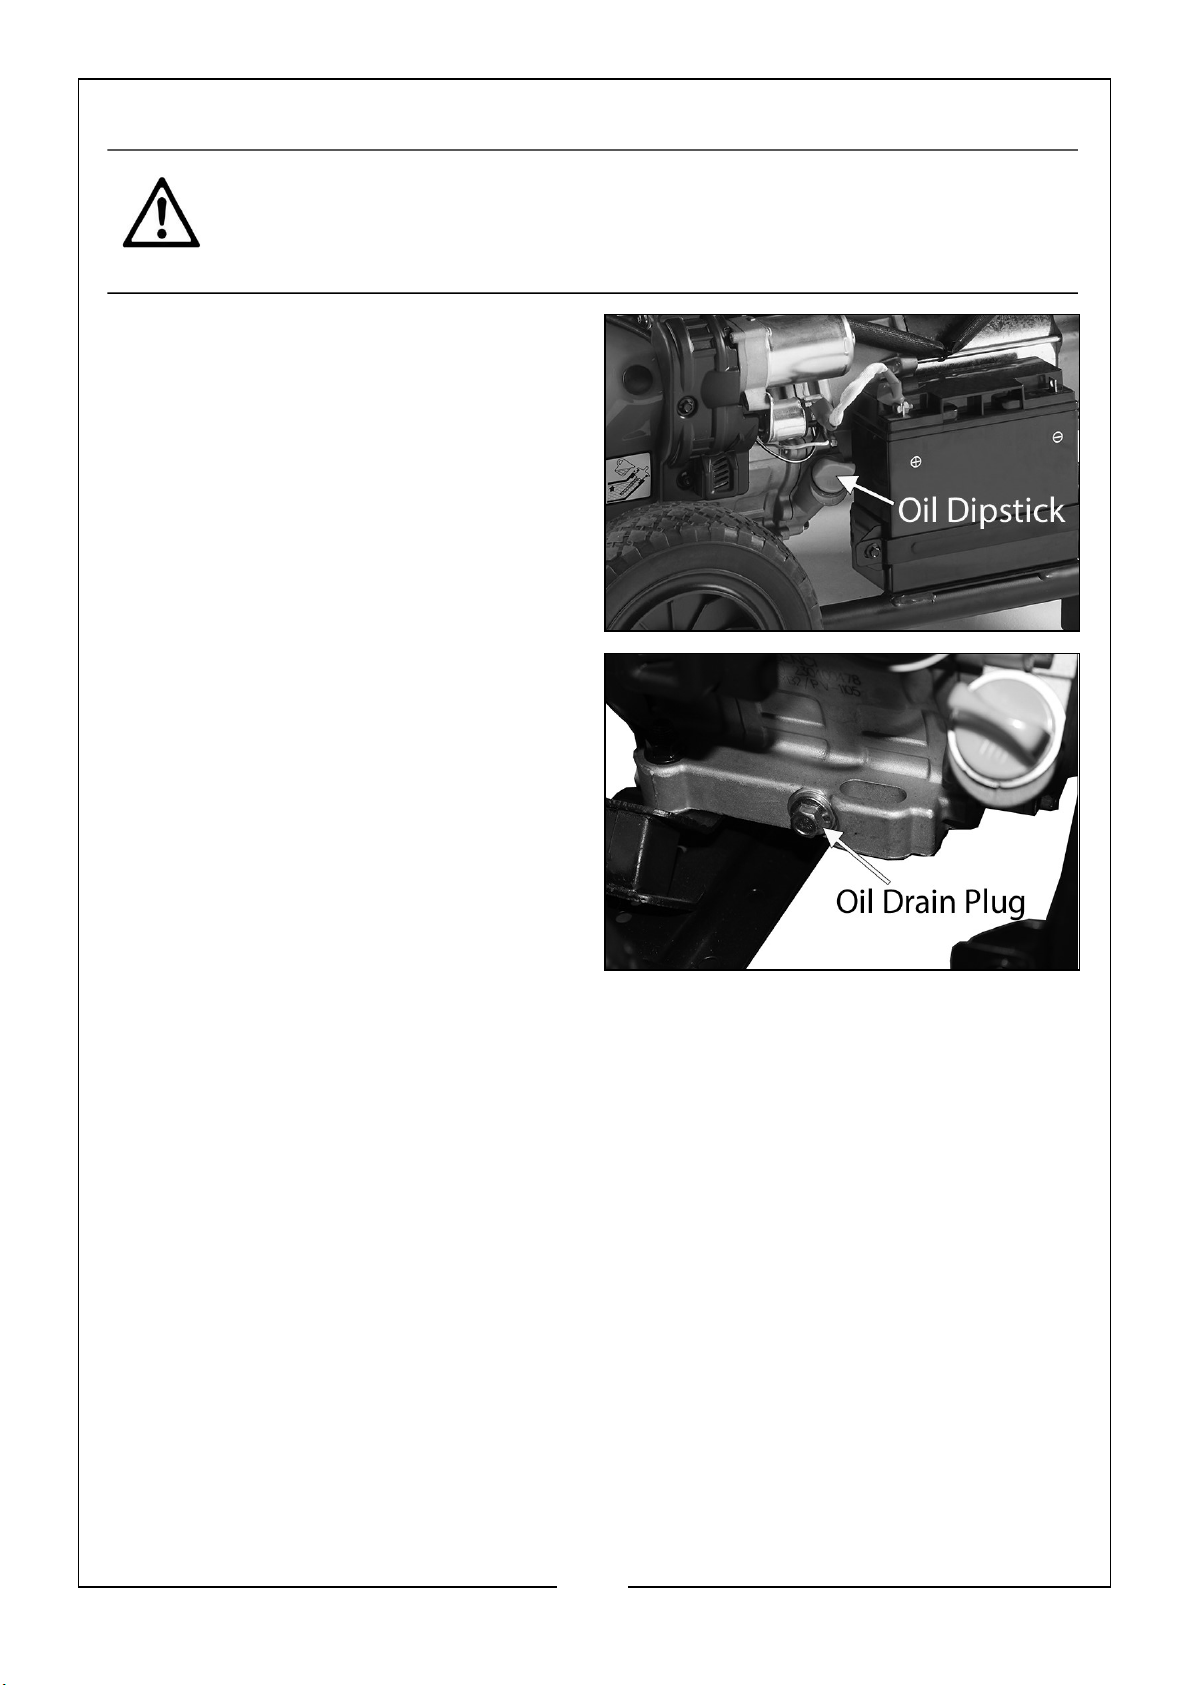
1. Unscrew and remove the oil filler
cap/dipstick.
2. Place an oil collection tray under the
drain plug.
3. Unscrew the drain plug and allow the
used engine oil to drain from the
crankcase into the oil collection tray.
NOTE: Drain the engine oil when the
engine is warm, this will ensure
the oil flows out faster.
4. Replace the drain plug.
5. Fill the crankcase with new engine
oil.
• Fill until the oil reaches the threads in the oil fill tube.
• Oil capacity: 1.1 Litre.
• We recommend the use of the following oil: CLARKE SAE 10W/30 Engine
Oil; Part No: 3050845
6. Replace the oil filler cap/dipstick.
ENVIRONMENTAL PROTECTION
One of the most damaging sources of pollution is oil, DO NOT throw away used
engine oil in with your domestic rubbish or pour it down drains or sinks. Place it in a
leak proof container and take it to your local waste disposal site.
32
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 33
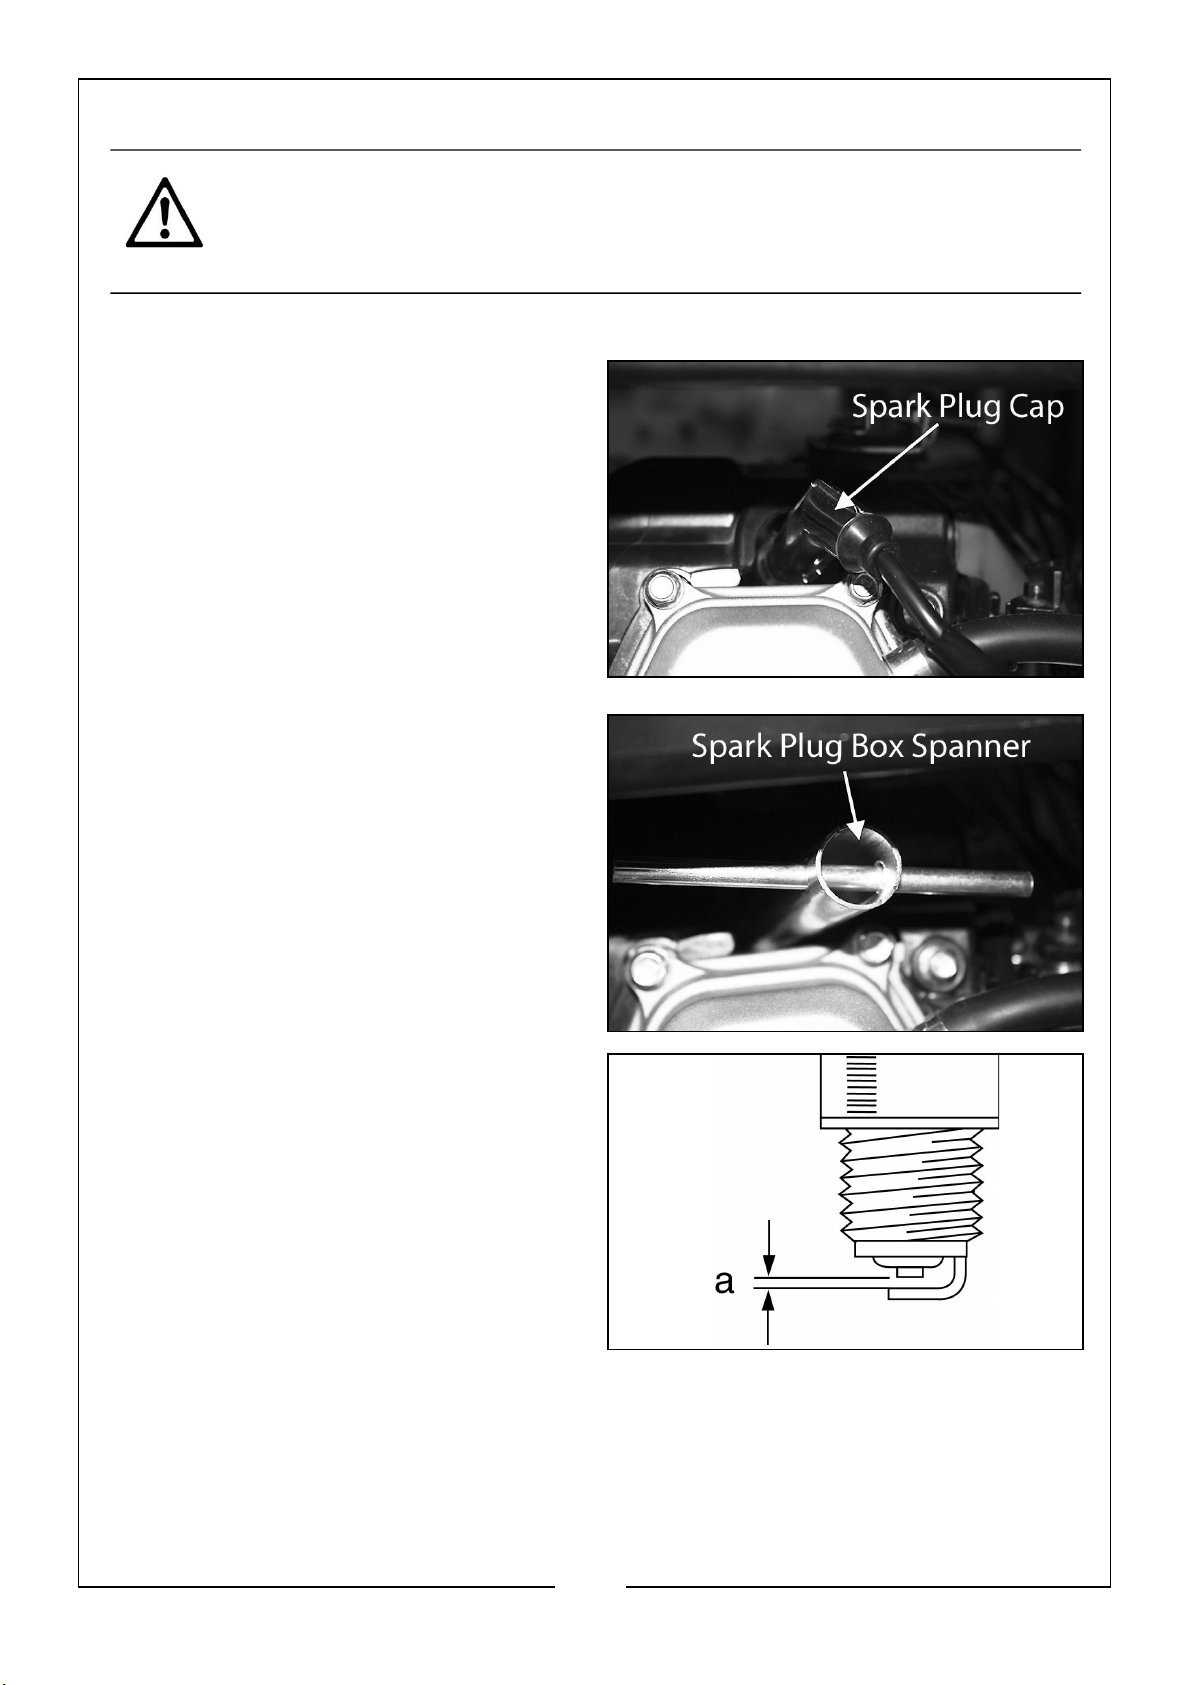
CHANGING THE SPARK PLUG
CAUTION: ALLOW THE ENGINE TO COOL BEFORE REMOVING THE SPARK
PLUG.
1. Remove the Side Panel bolts and remove the side panel
2. Remove the spark plug cap from the
spark plug.
3. Use the spark plug box spanner
supplied to remove the spark plug.
4. Remove any carbon that has
accumulated around the electrode.
5. Check the spark plug gap (a), it
should be between 0.7 and 0.8 mm,
adjust if necessary.
6. Check the overall condition of the
spark plug for erosion or pitting and
replace if necessary.
7. Reinstall the spark plug and replace
the spark plug cap.
33
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 34
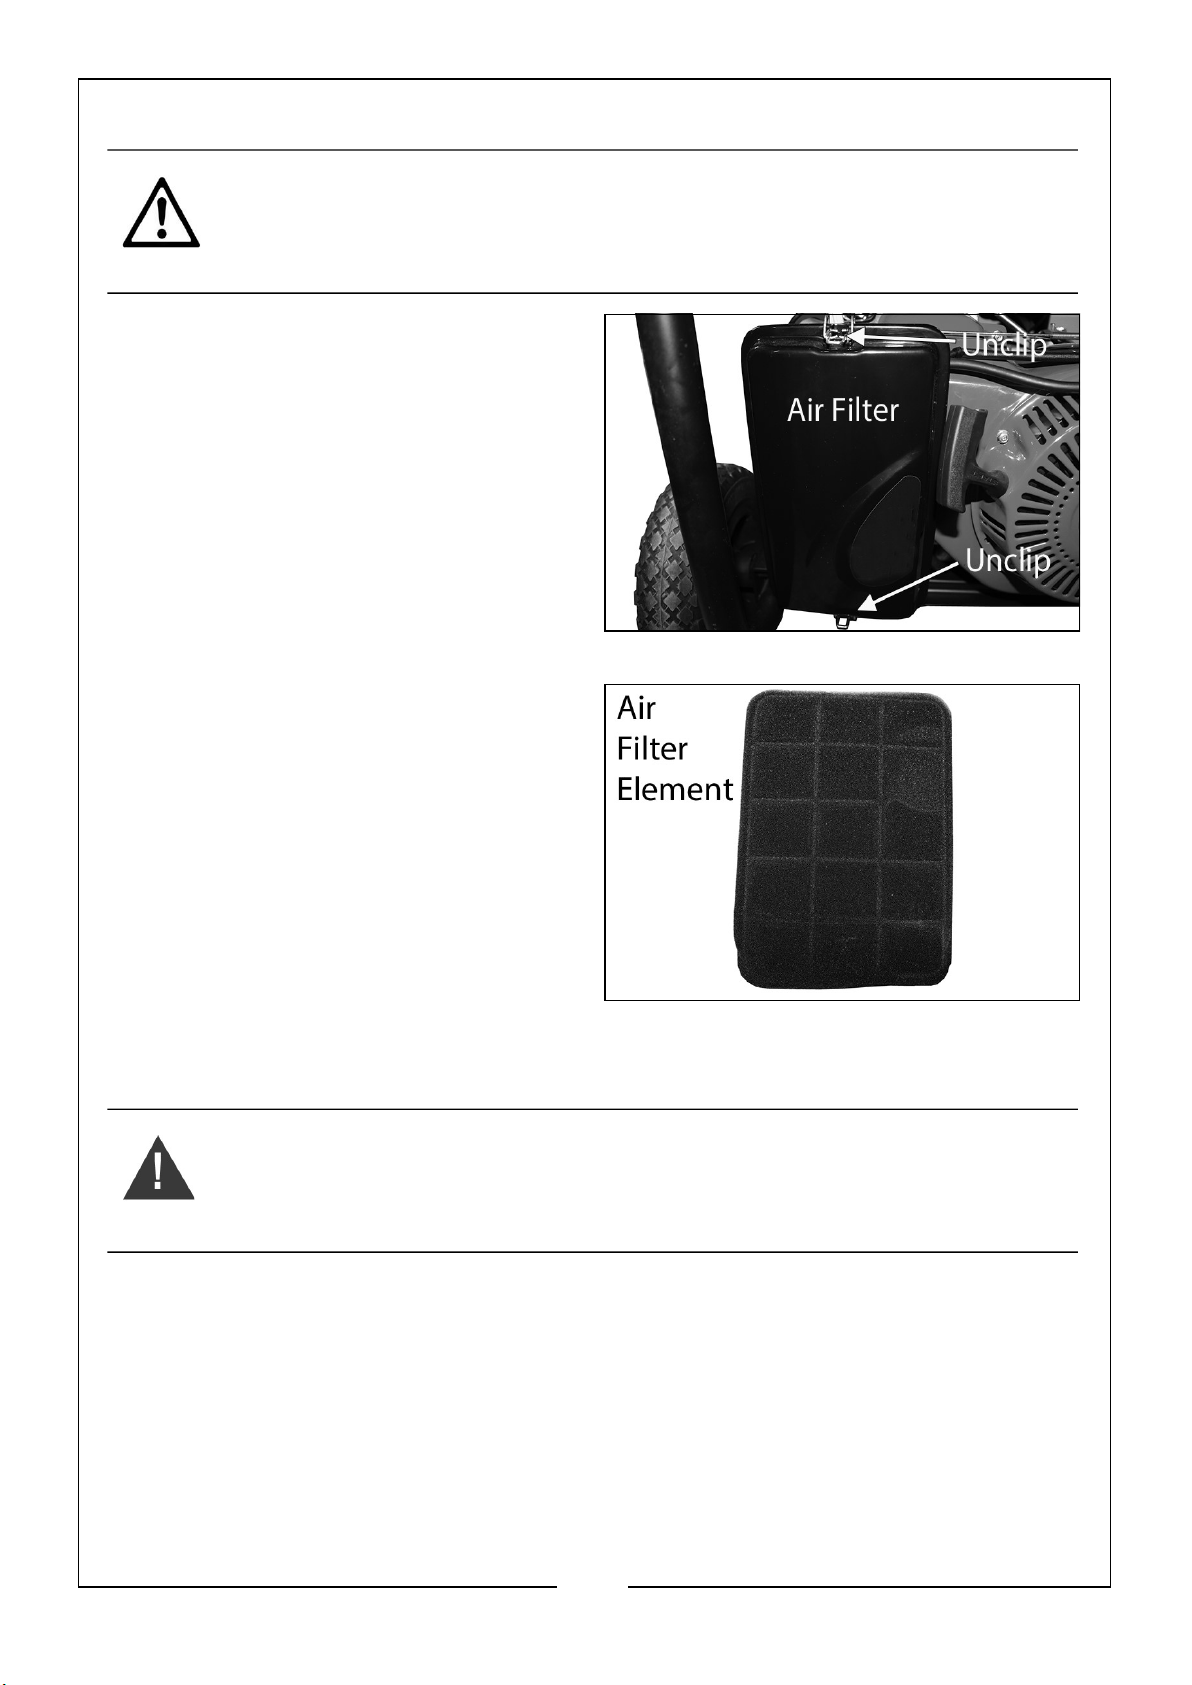
CHECKING THE AIR FILTER
CAUTION: DO NOT USE THE GENERATOR WITHOUT THE AIR FILTER
FITTED, THIS CAN DAMAGE THE GENERATOR.
1. Unclip and remove the air filter cover.
2. Remove the air filter element.
3. Make sure that the air filter is clean
and not damaged.
• If the air filter is damaged contact
CLARKE spare parts department
for a replacement.
• If the filter is dirty, wash in a
solution of warm water and mild
detergent and rinse thoroughly.
Leave the filter to dry completely,
once it is dry immerse in clean engine oil and squeeze to remove excess
oil.
WARNING: DO NOT USE INFLAMMABLE SOLVENTS OR PETROL TO
CLEAN THE AIR FILTER.
4. Replace the filter to its original position and replace the air filter cover.
34
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 35
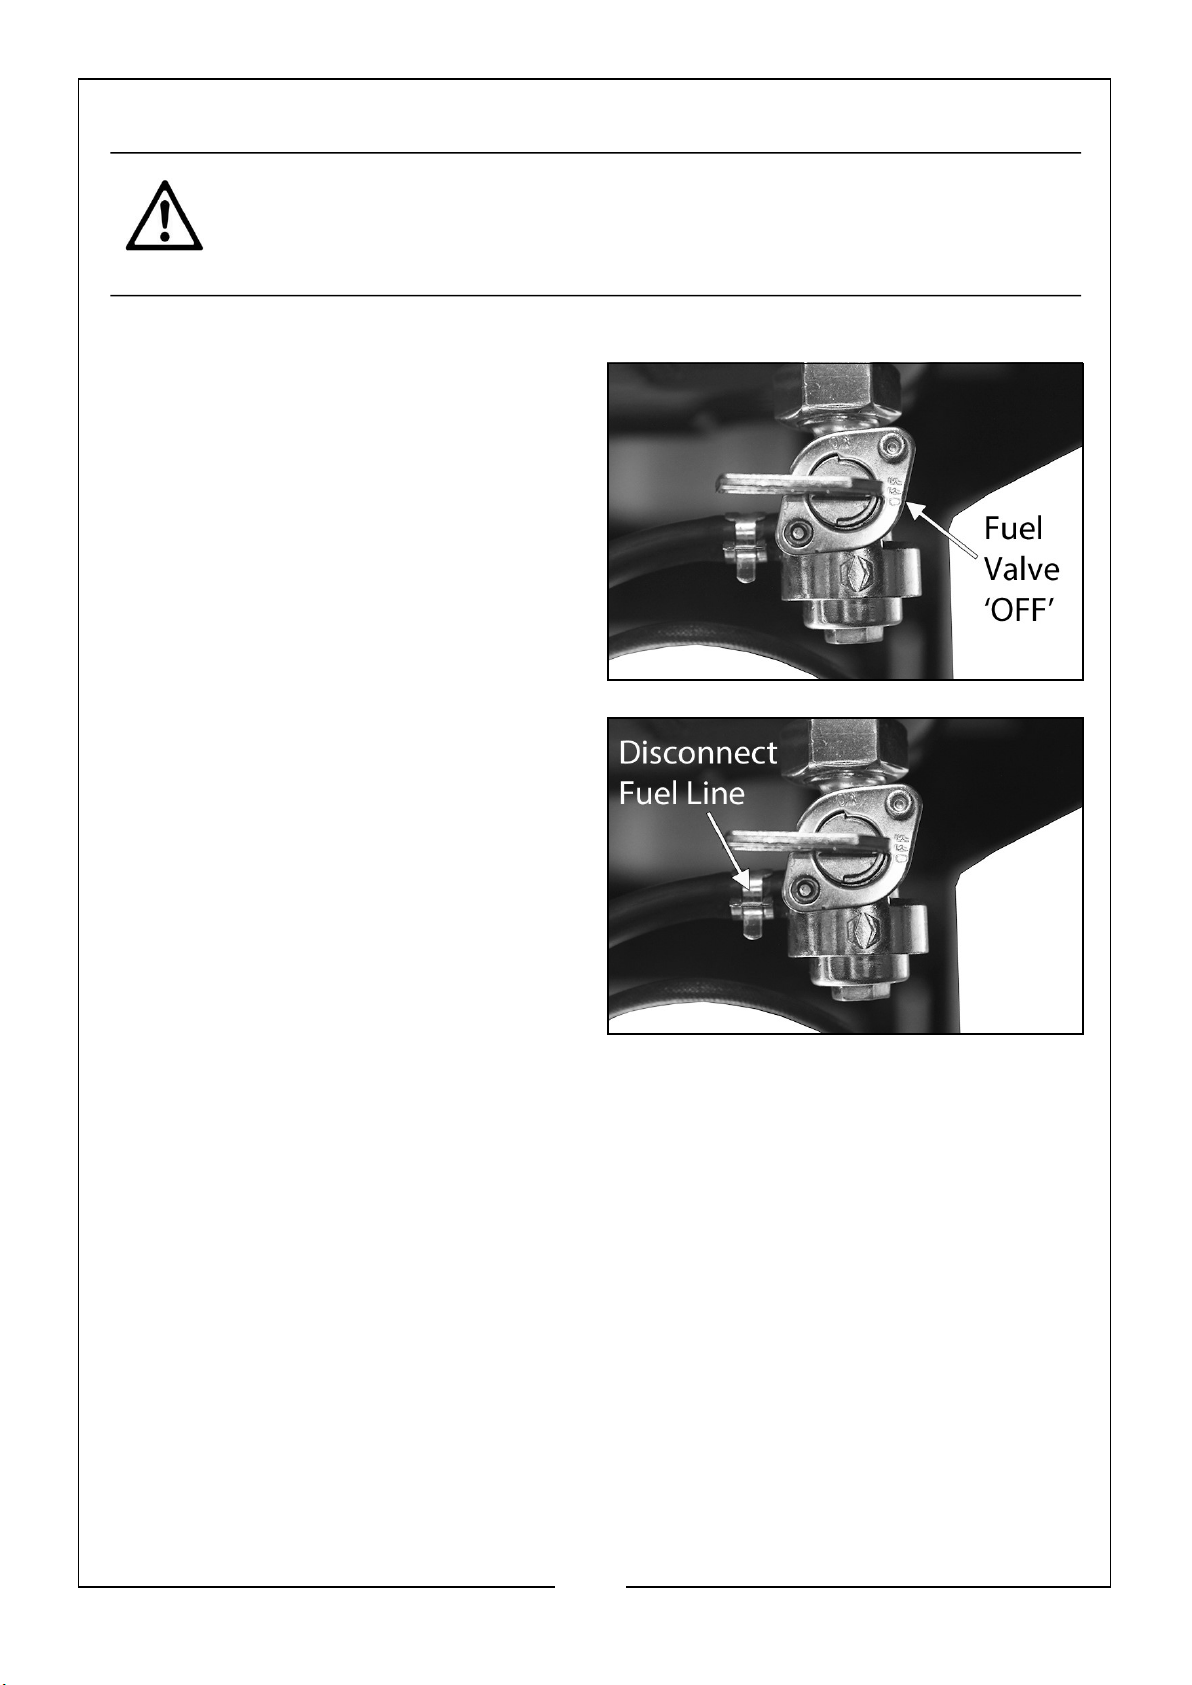
CLEANING/DRAINING THE FUEL TANK
CAUTION: ALWAYS CARRY THIS PROCEDURE OUT IN A WELL
VENTILATED AREA AND AWAY FROM ANY NAKED FLAME OR HEAT
SOURCE.
• You will need a length of 7mm external diameter tubing.
1. Set the fuel valve to the ‘OFF’
position.
2. Disconnect the fuel supply line by
pinching the tube clip and pulling the
supply line off the fuel valve.
3. Attach the 7mm external diameter
tubing to the bottom outlet of the
fuel valve.
4. Place an approved petrol storage
container under the tubing and turn
the fuel valve to the ‘ON’ position.
• The fuel in the tank will drain into
the container.
5. Once the fuel tank is empty turn the fuel valve to the ‘OFF’ position and reconnect
the fuel supply line.
35
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 36
MAINTENANCE RECORD
ENGINE OIL (PAGE 10 & 32)
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
AIR FILTER (PAGE 34)
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
SPARK PLUG (PAGE 33)
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
FUEL FILTER (PAGE 11-12)
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
BI-ANNUAL SERVICE
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
_____________________________________________________________________
36
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 37
STORAGE
1. Disconnect all appliances and welding cables when not in use.
2. Always store in a clean dry place.
LONG TERM STORAGE
For long term storage;
1. The petrol tank should be drained. See page 35.
• Ensure that the engine is cold before draining the tank.
2. DO NOT store petrol for long periods of time.
3. Dispose of excess petrol and oil in an environmentally safe way. Your local
recycling centre can advise you on the best method of disposal.
4. After the petrol tank has been drained, start the engine and allow it to use any
petrol that may remain in the engine, carburetor or fuel pipe.
37
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 38
TROUBLESHOOTING
If the following does not solve your problem contact the CLARKE service dept.
PROBLEM CAUSE SOLUTION
Engine will not
start (see engine
manual for
further engine
troubleshooting
No Output from
Generator
Low voltage on the
battery
Fuel valve not open Open fuel valve
Chock valve not open Open choke valve
Low oil level Check oil level, add oil if required
Oil warning system
problem
Bad fuel Change fuel
Oil clogging Check that the correct oil is being used.
Ignition system problem Check and clean spark plug
Carburetor problem Clean or repair carburetor
Voltage meter broken Contact CLARKE service centre for repair.
Charge or change the battery
If not, drain oil and replace with correct
oil
DO NOT use until repaired
Alternator leading wire
and/or control panel
wire not connected
Brush and slip ring do
not connect well or are
disconnected
Control panel broken Contact CLARKE service centre for repair.
Short circuit, open circuit
or grounded wire
Circuit breaker not open Open circuit breaker
Contact CLARKE service centre for repair.
DO NOT use until repaired
Clean and/or replace slip ring and brush.
Contact CLARKE service centre for repair.
DO NOT use until repaired
Inspect and repair, or replace alternator
winding. Contact CLARKE service centre
for repair.
38
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 39
PROBLEM CAUSE SOLUTION
Output Voltage
High or Low
Current High or
Low or Cant
Adjust
Alternator
Smoking
High or low rotate speed Have engine speed adjusted. Contact
CLARKE service centre
AVR Problem Have AVR checked and replaced if
needed. Contact CLARKE service centre
High or low rotate speed Have engine speed adjusted. Contact
CLARKE service centre
Short circuit, open circuit
or grounded wire
Inspect and repair, or replace alternator
winding. Contact CLARKE service centre
for repair.
MDS or rectifier diode
short circuit or grounded
Replace MDS module and/or rectifier
diode. Contact CLARKE service centre
AVR Problem Replace AVR. Contact CLARKE service
centre
Rotor and stator rub Replace or repair rotor and/or
stator.Contact CLARKE service centre
Overload Remove some of the load appliances
Winding short circuit or
grounded
MDS or rectifier diode
short circuit or grounded
Replace alternator winding. Contact
CLARKE service centre
Replace MDS module and/or rectifier
diode. Contact CLARKE service centre
39
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 40
PRODUCT SPECIFICATIONS
Welding Specifications
Output (Min/Max) 50-200amps
Open Circuit Voltage 22-28V
IP Rating IP21S
Welding Rod Capacity 1.6 - 4.00mm
Duty Cycle 60%
Ambient Temperature
Insulation Class H
Engine Specifications
Make & Model/Type Senci SC420/Petrol
Capacity 420cc
Revs Per Minute (RPM) 3600
Engine Power 9.5 kW/14 HP
Fuel Tank Capacity 18 Litres (Safe Capacity)
Oil Capacity/ Grade 1.1 Litres/ SAE10W-30
Spark Plug Type F7RTC
Battery Type 12 V/18 Ah/Wet Sealed
Fuel Consumption 2.8 L/hr
Run Time @75% Power 6.5 Hours
Cooling System Air
-10oC~40oC (-14oF~104oF)
Choke Type Manual
Emissions: CO (g/kWh) 278.05
HC (g/kWh) 2.52
NOx (g/kWh) 3.09
HC + NOx (g/kWh) 5.61
Electrical Specifications
Rated Output Power 5kW
Max Rated Output 5.5kW
Rated Output Current 21.7 A
Max. Rated Output Current 23.9 A
AC Output Voltage 1 x 230V~50Hz, 1 x 110V~50Hz
40
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 41
DC Output Voltage 75V
Operating Temperature
-10oC~40oC (-14oF~104oF)
Number of Sockets 1 x 110V 32A (IP44) & 1 x 230V 32A (IP44)
Noise Emissions
Sound Pressure Level (dB: LpA) TBC
Sound Power Level (dB: LwA) TBC
Guaranteed Sound Power Level (dB: LwA) TBC
Uncertainty Factor (K) TBC
Dimension/Weights
Product (LxWxH) 760mm x 710mm x 690mm
Weight 100kg
41
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 42
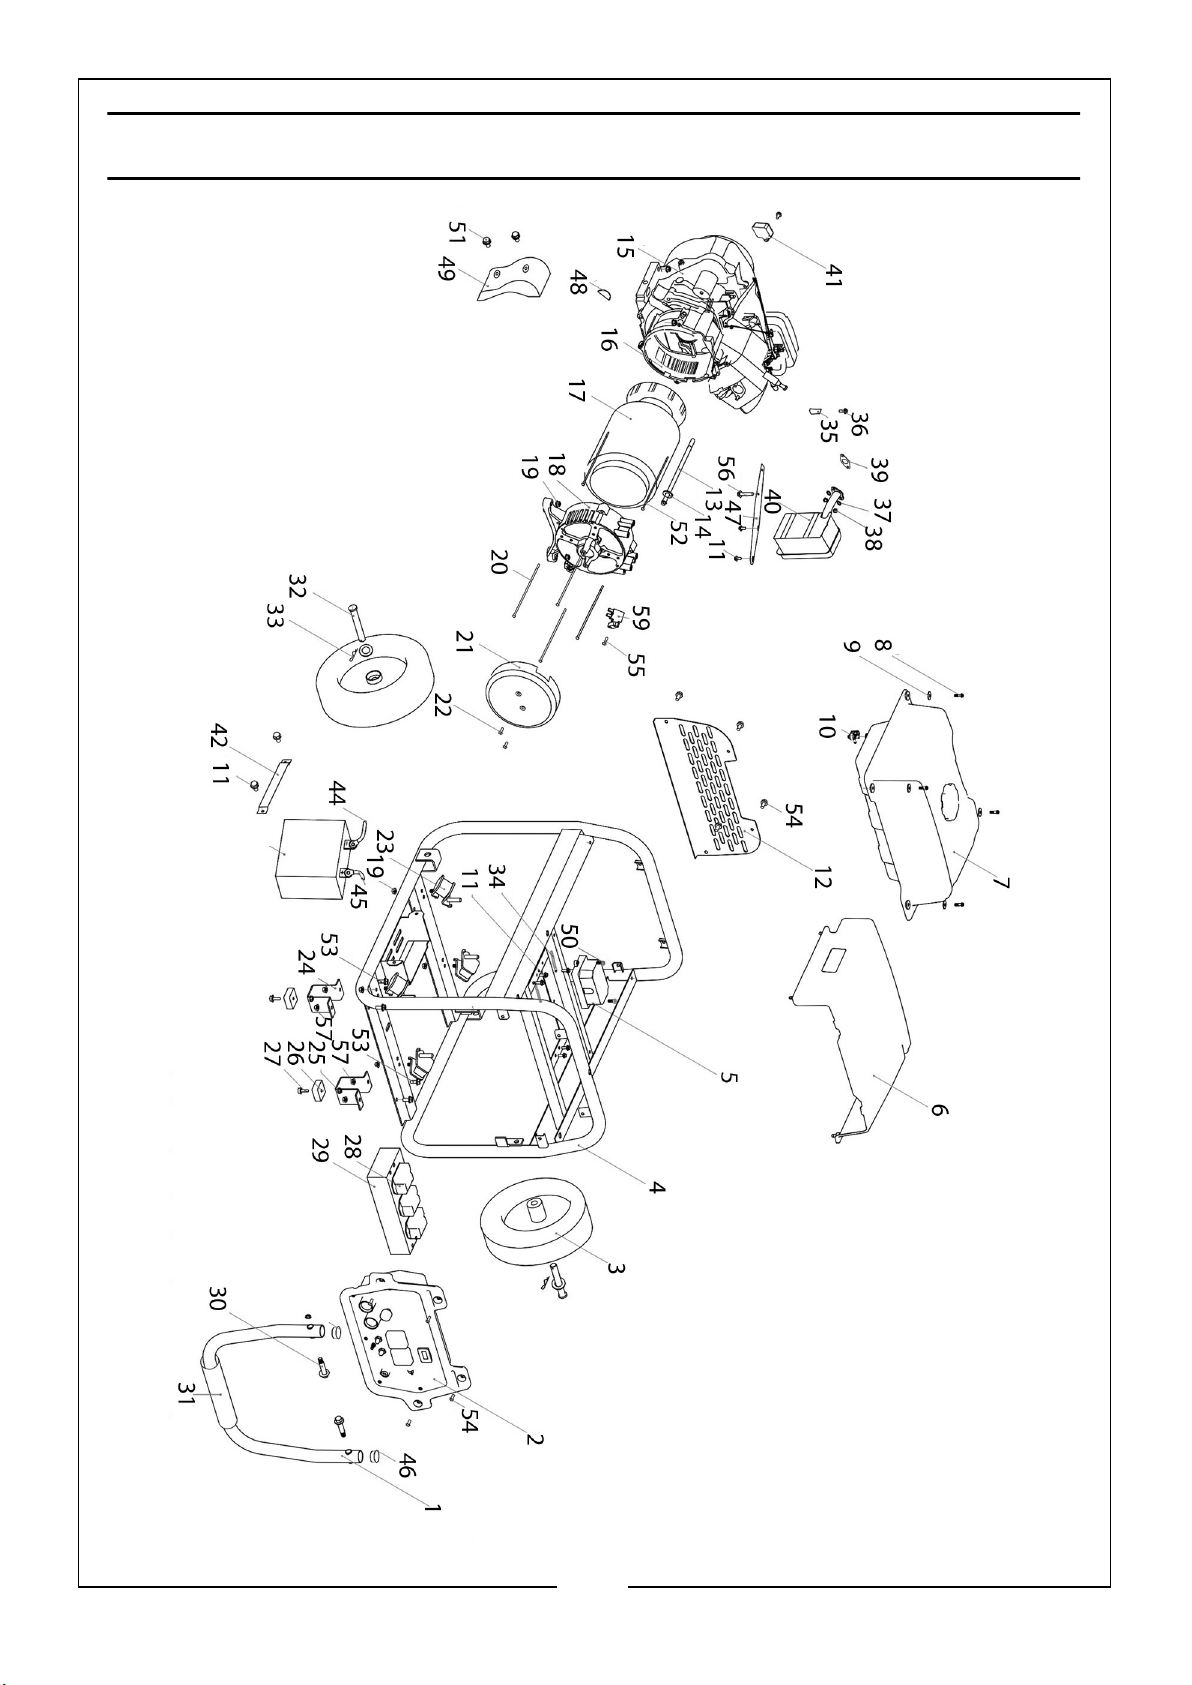
EXPLODED DIAGRAM - GENERATOR
42
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 43
PARTS LIST - GENERATOR
NO DESCRIPTION NO DESCRIPTION
1 Handle 31 Handle Grip
2 Control Panel 32 Wheel Axle x 2
3 Wheel x 2 33 Wheel Clip Pin x 2
4 Frame 34 Wire Clip x 2
5 Automatic Voltage Regulator 35 Crankshaft Dustproof Cover
6 Engine Hood 36 M6 Flange Bolt x 2
7 Fuel Tank Assembly 37 Spring Washer x 2
8 M6 Flange Bolt x 4 38 M8 Hex Bolt x 2
9 Tank Cushion Washer x 4 39 Muffler Washer
10 Fuel Cock Assembly 40 Muffler
11 M6 Flange Bolt x 10 41 Charger
12 Side Panel 42 Battery Tension Plate
13 M10 Flange Bolt 43 12V 12Ah Battery
14 10.5 x 20 x 1.5 Flat Washer 44 Battery Negative Wire
15 Engine Assembly 45 Battery Positive Wire
16 Crankshaft Cover 46 Frame Plug x 2
17 Alternator 47 Muffler Support
18 Alternator Bracket 48 Rubber Cap
19 M10 Flange Bolt x 4 49 Wire Cover
20 M6 Flange Bolt x 4 50 M5 Hex Cap Screw x 2
21 Alternator End Cover 51 M6 Flange Bolt x 2
22 M5 Flange Bolt x 5 52 M5 Flange Bolt x 2
23 Rubber Seat x 4 53 M8 Flange Bolt x 4
24 Support x 2 54 M6 Flange Bolt x 8
25 M6 Flange Bolt x 5 55 M5 Flange Bolt
26 Rubber Seat Support x 2 56 M8 Flange Bolt
27 M6 Flange Bolt x 2 57 M8 Flange Bolt x 5
28 Rectifier 58 17 x 30 x 2.5 Flat Washer x 2
29 Radiator
30 Handle Dowel Pin x 2
43
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 44
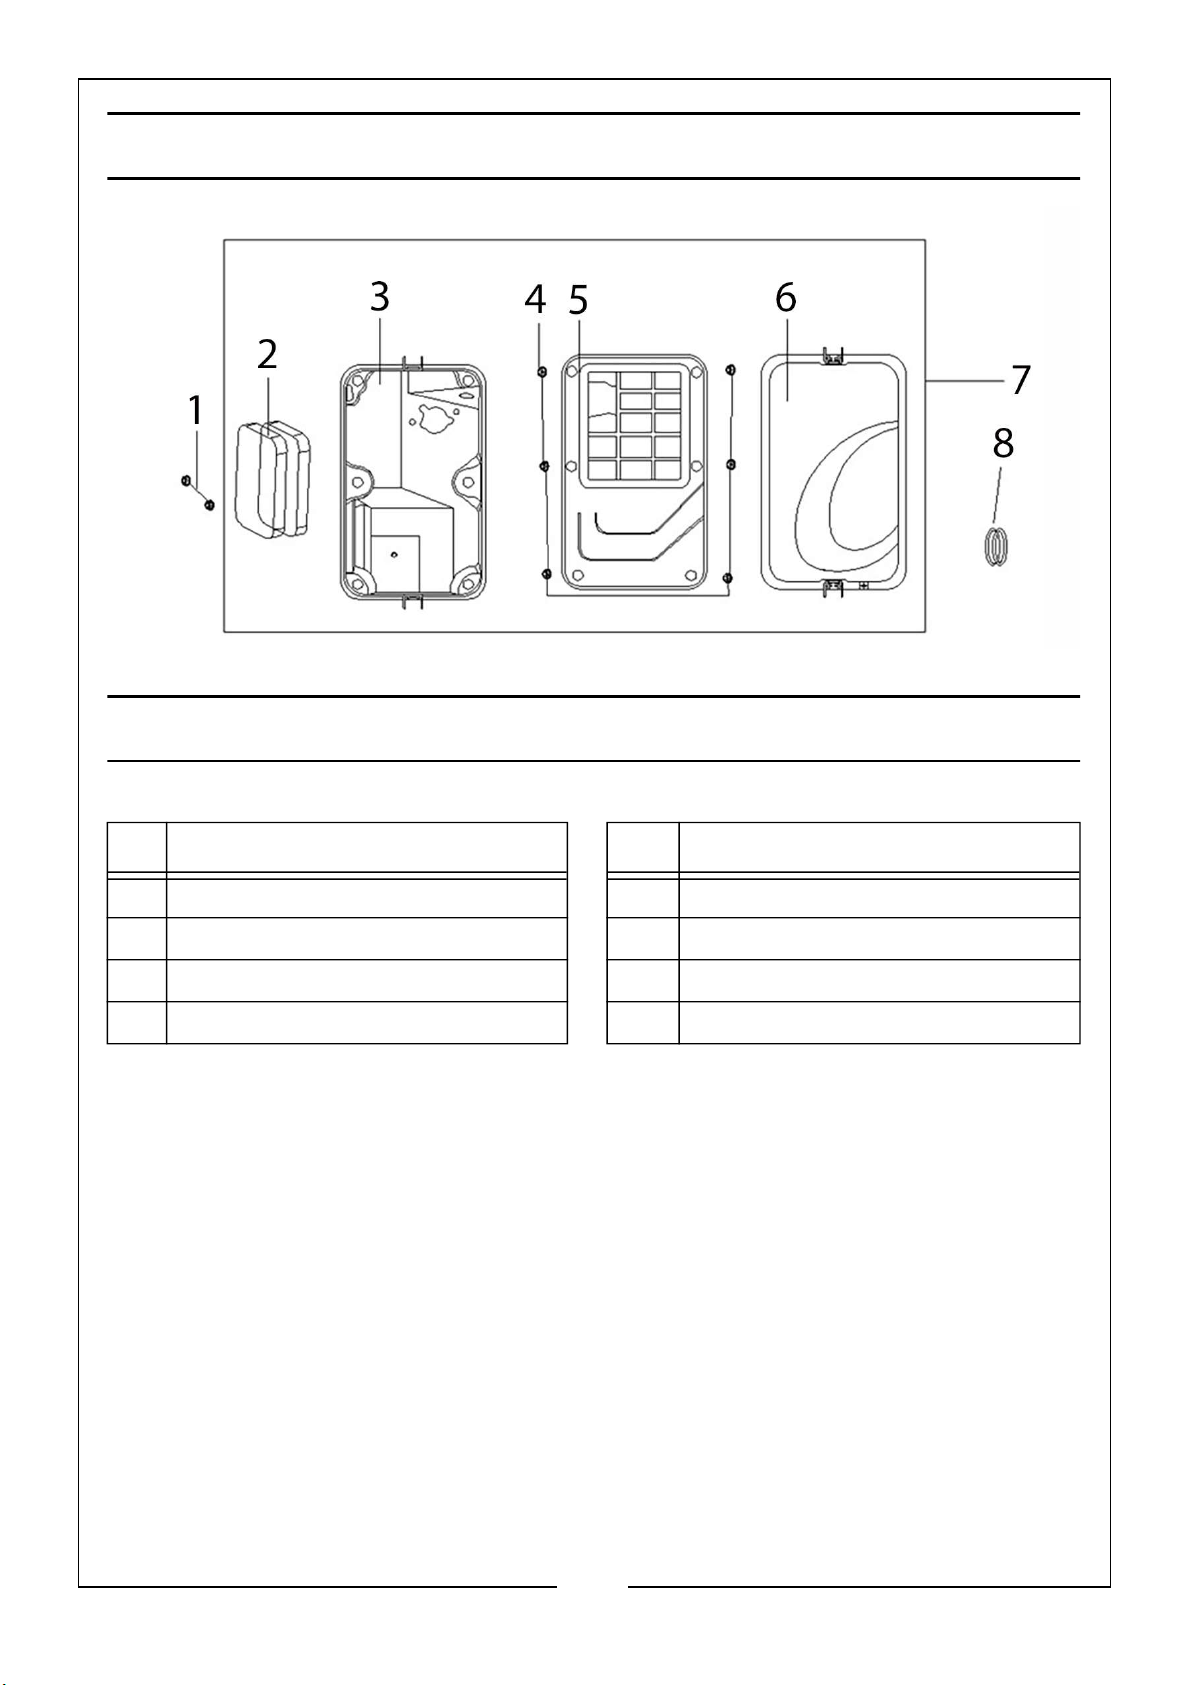
EXPLODED DIAGRAM - AIR FILTER
PARTS LIST - AIR FILTER
NO DESCRIPTION NO DESCRIPTION
1 Flange Bolt x 2 5 Air Filter Element Support
2 Air Filter Element Assembly x 2 6 Air Filter Back Cover
3 Air Filter Front Cover 7 Air Filter Assembly
4 Flange Bolt x 6 8 Fuel Pipe Sleeve
44
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 45
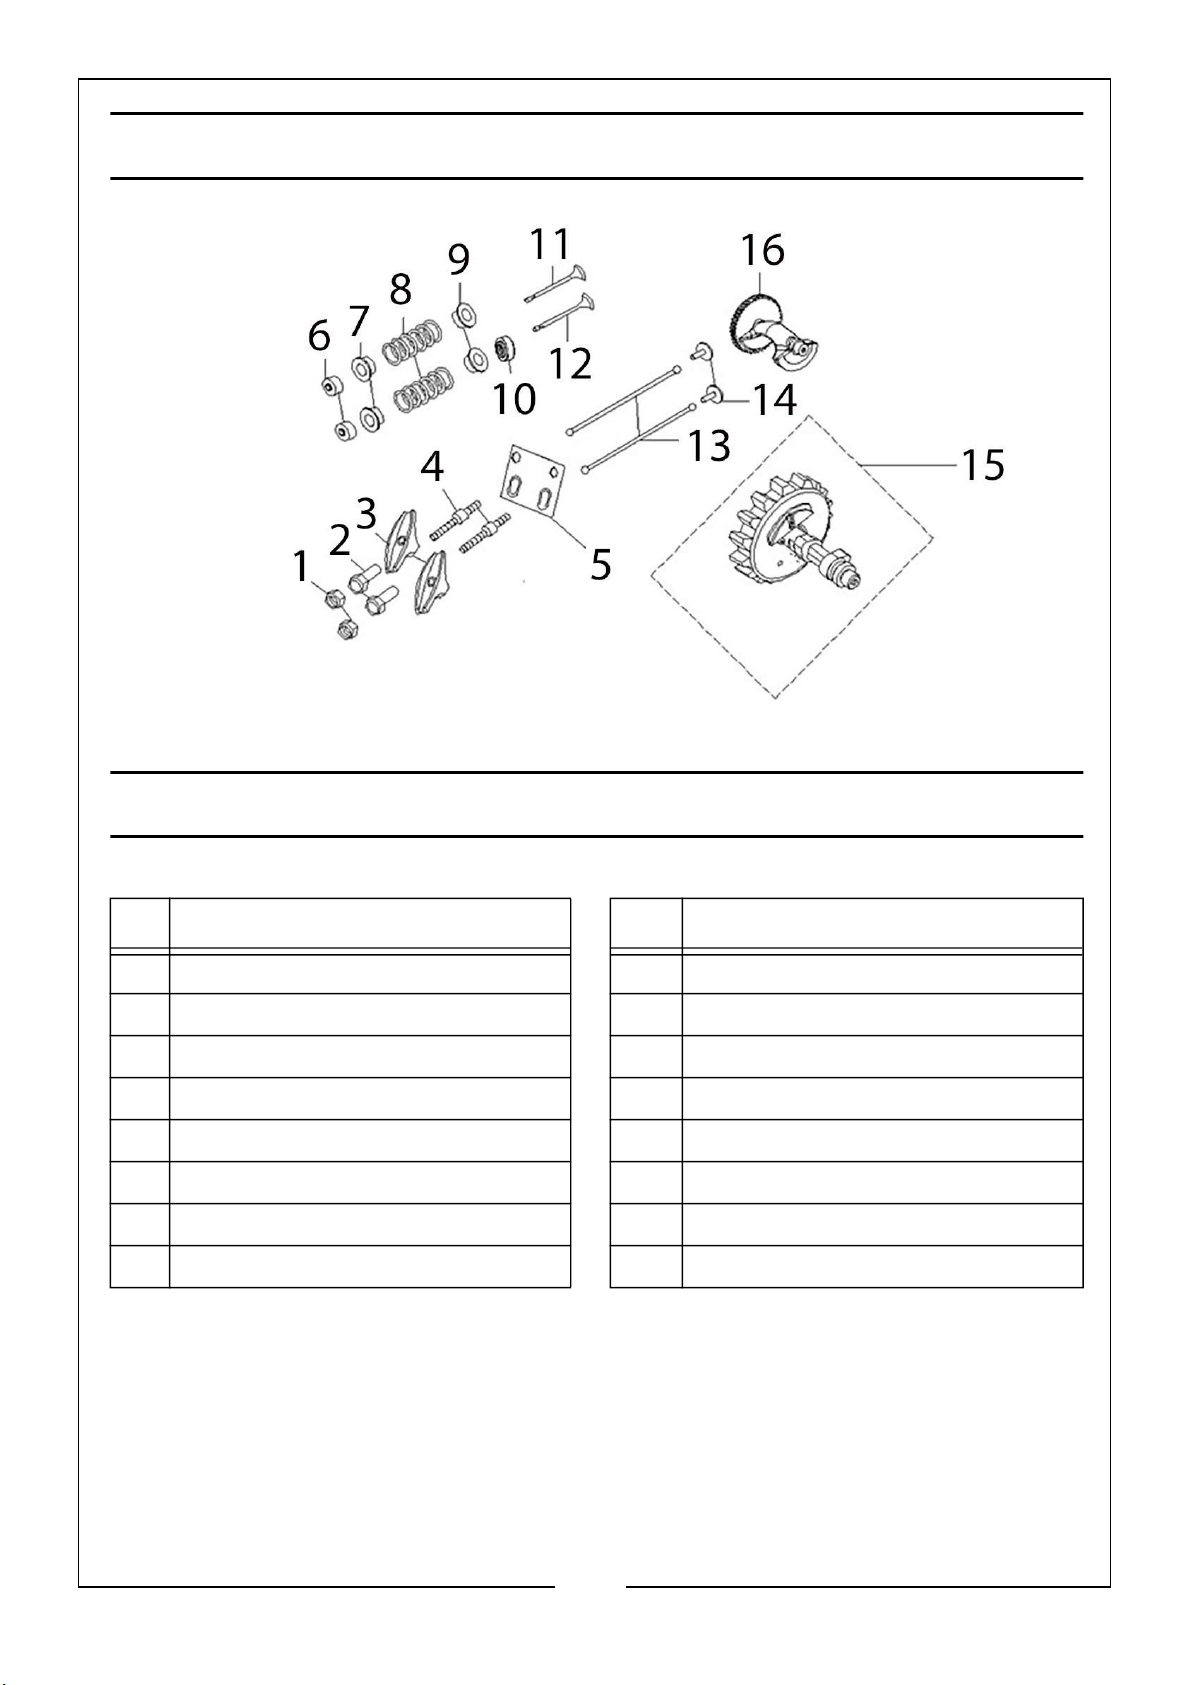
EXPLODED DIAGRAM - CAMSHAFT
PARTS LIST - CAMSHAFT
NO DESCRIPTION NO DESCRIPTION
1 Valve Adjusting Nut x 2 9 Retainer Valve, Bottom x 2
2 Rocker Shaft x 2 10 Oil Seal x 2
3 Rocker Arm x 2 11 Valve, Exhaust
4 Bolt Valve x 2 12 Valve, Intake
5 Push Rod Guide Plate 13 Push Rod x 2
6 Rotator Valve x 2 14 Lifter Valve x 2
7 Retainer Valve Spring x 2 15 Camshaft Assembly
8 Spring Valve x 2 16 Balance Shaft
45
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 46
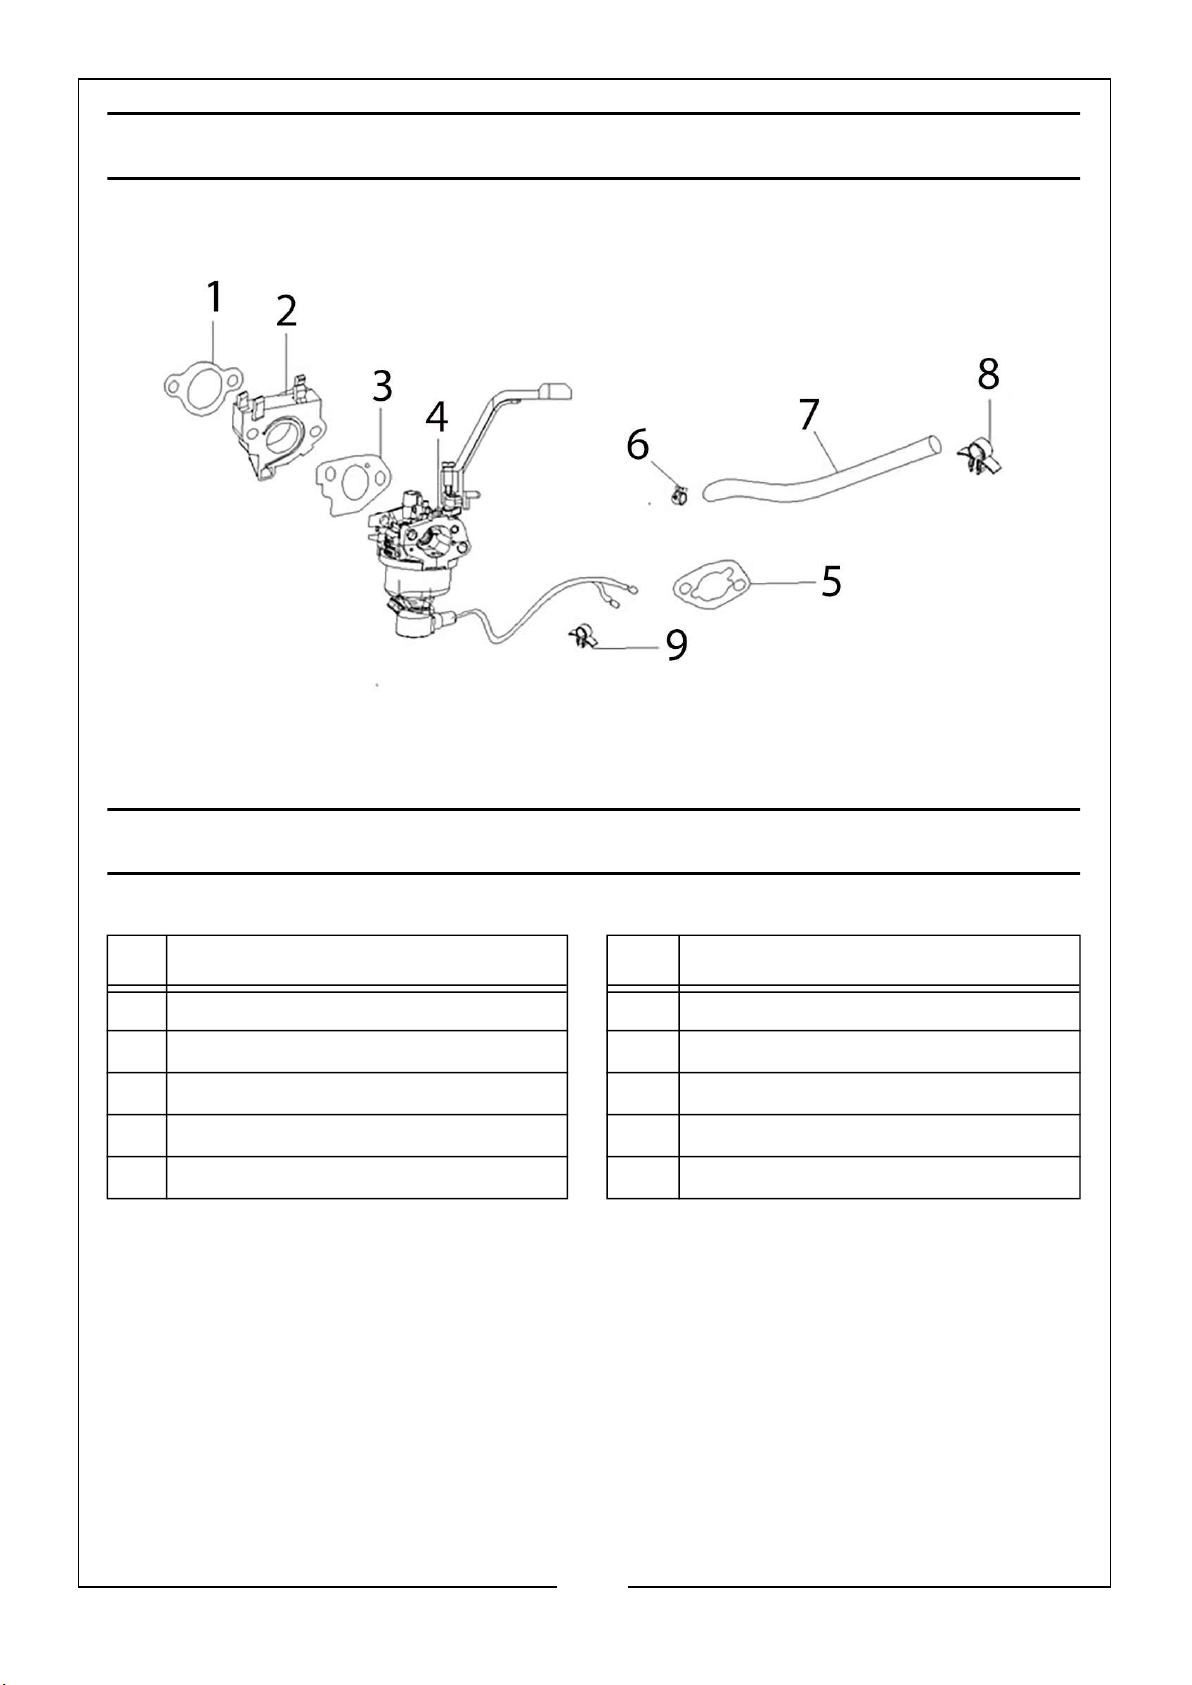
EXPLODED DIAGRAM - CARBURETOR
PARTS LIST - CARBURETOR
NO DESCRIPTION NO DESCRIPTION
1 Gasket, Intake 6 Fuel Pipe Clip
2 Carburetor Insulator 7 180cm Fuel Pipe
3 Carburetor Gasket 8 Fuel Pipe Clip
4 Carburetor 9 Fuel Pipe Clip
5 Air Filter Gasket
46
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 47
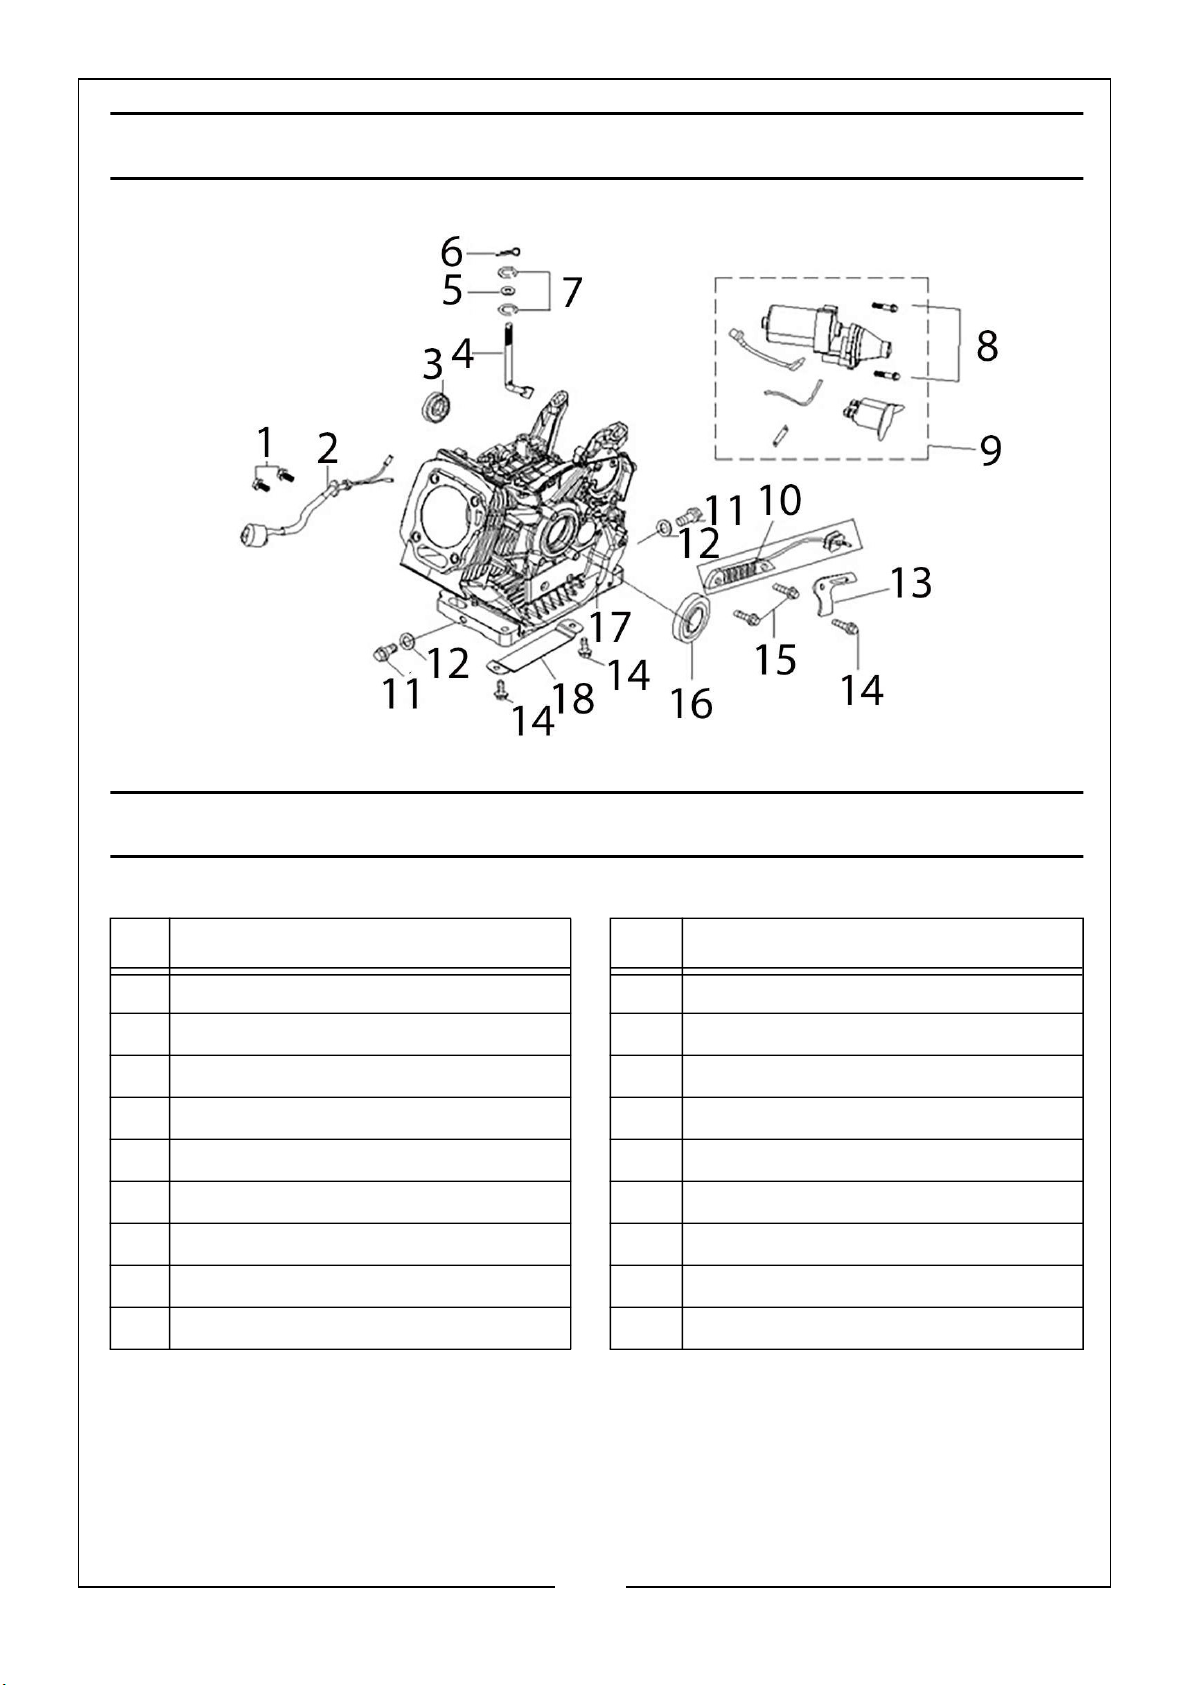
EXPLODED DIAGRAM - CRANKCASE ASSEMBLY
PARTS LIST - CRANKCASE ASSEMBLY
NO DESCRIPTION NO DESCRIPTION
1 Bolt x 2 10 Charging Coil
2 Engine Oil Sensor 11 Bolt x 2
3 Bearing 12 Washer x 2
4 Governor Shaft 13 Wire Pressing Board
5 Oil Seal 14 Bolt x 3
6 Lock Pin 15 Bolt
7 Washer x 2 16 Oil Seal
8 Bolt x 2 17 Crankcase
9 Starter Motor 18 Bracket
47
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 48
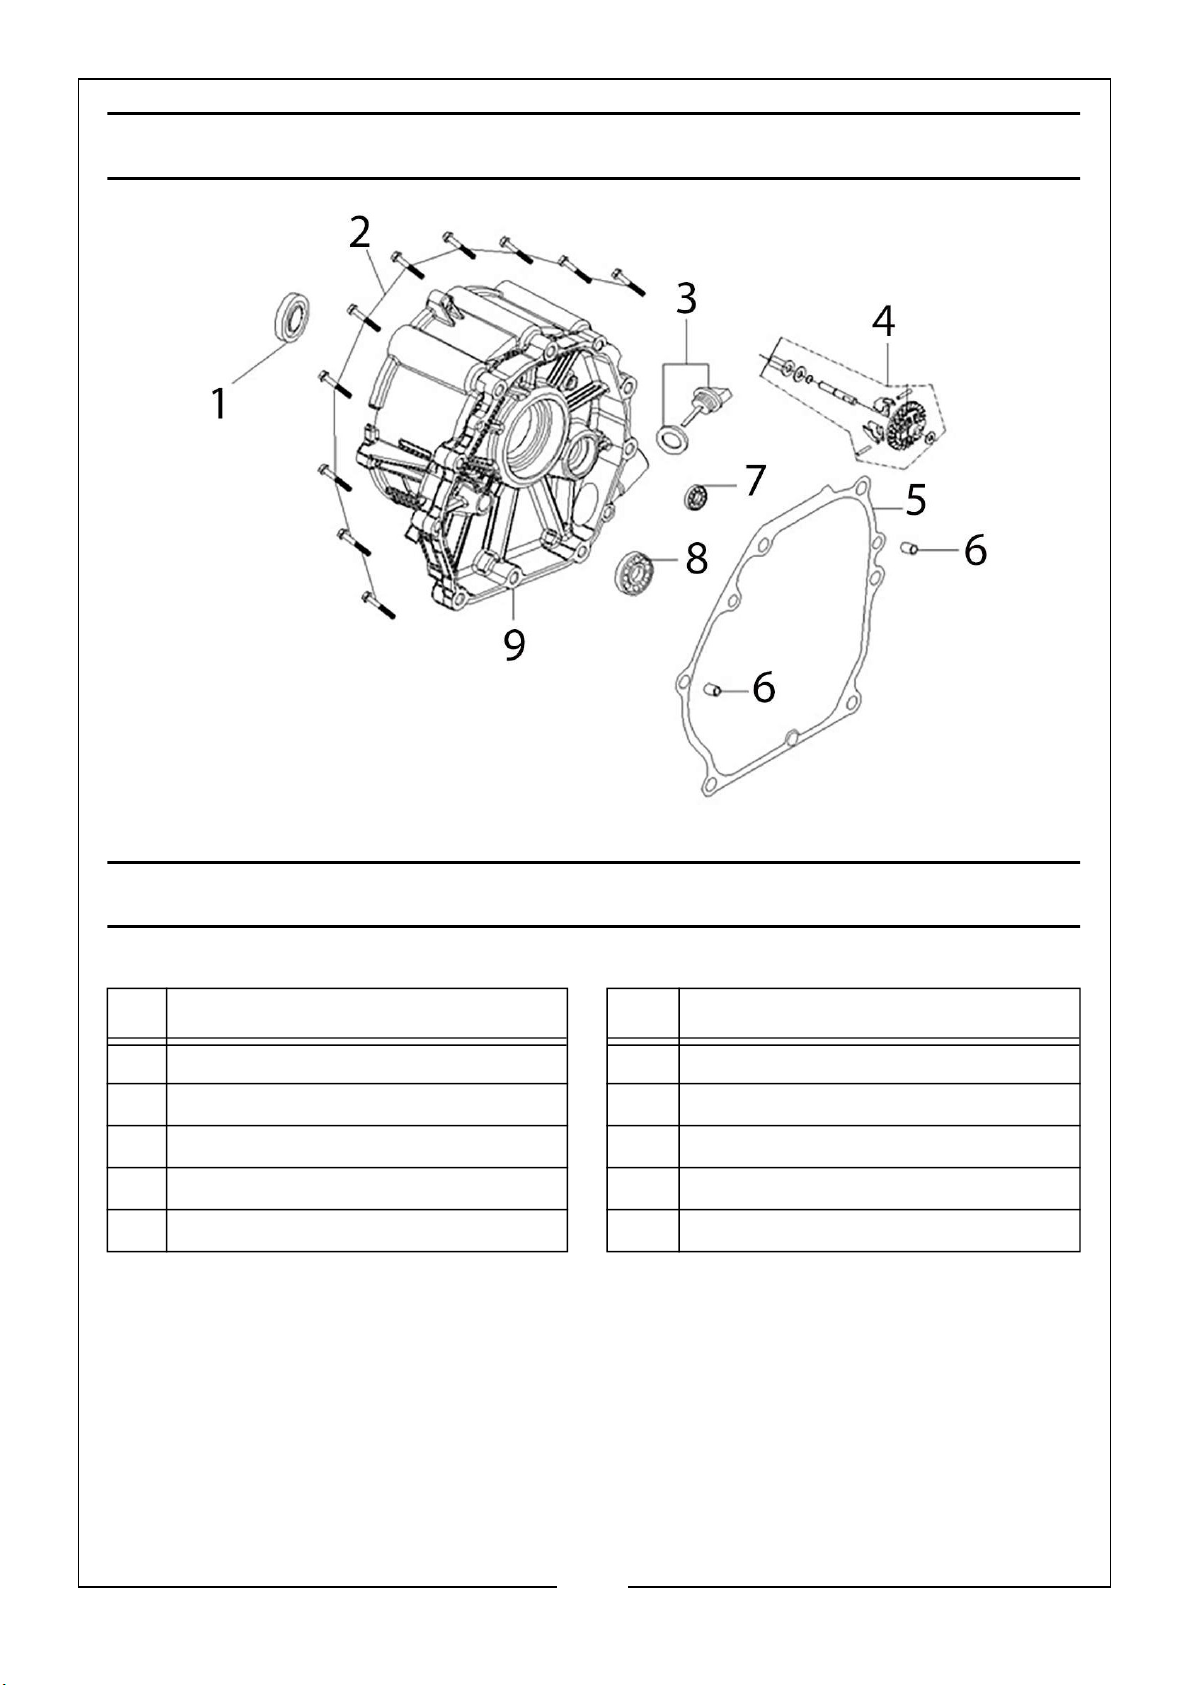
EXPLODED DIAGRAM - CRANKCASE COVER
PARTS LIST - CRANKCASE COVER
NO DESCRIPTION NO DESCRIPTION
1 Oil Seal 6 Dowel Pin x 2
2 Bolt x 10 7 Bearing
3 Dipstick Assembly 8 Bearing
4 Governor Gear Kit 9 Crankcase Cover
5 Gasket, Crankcase Cover
48
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 49
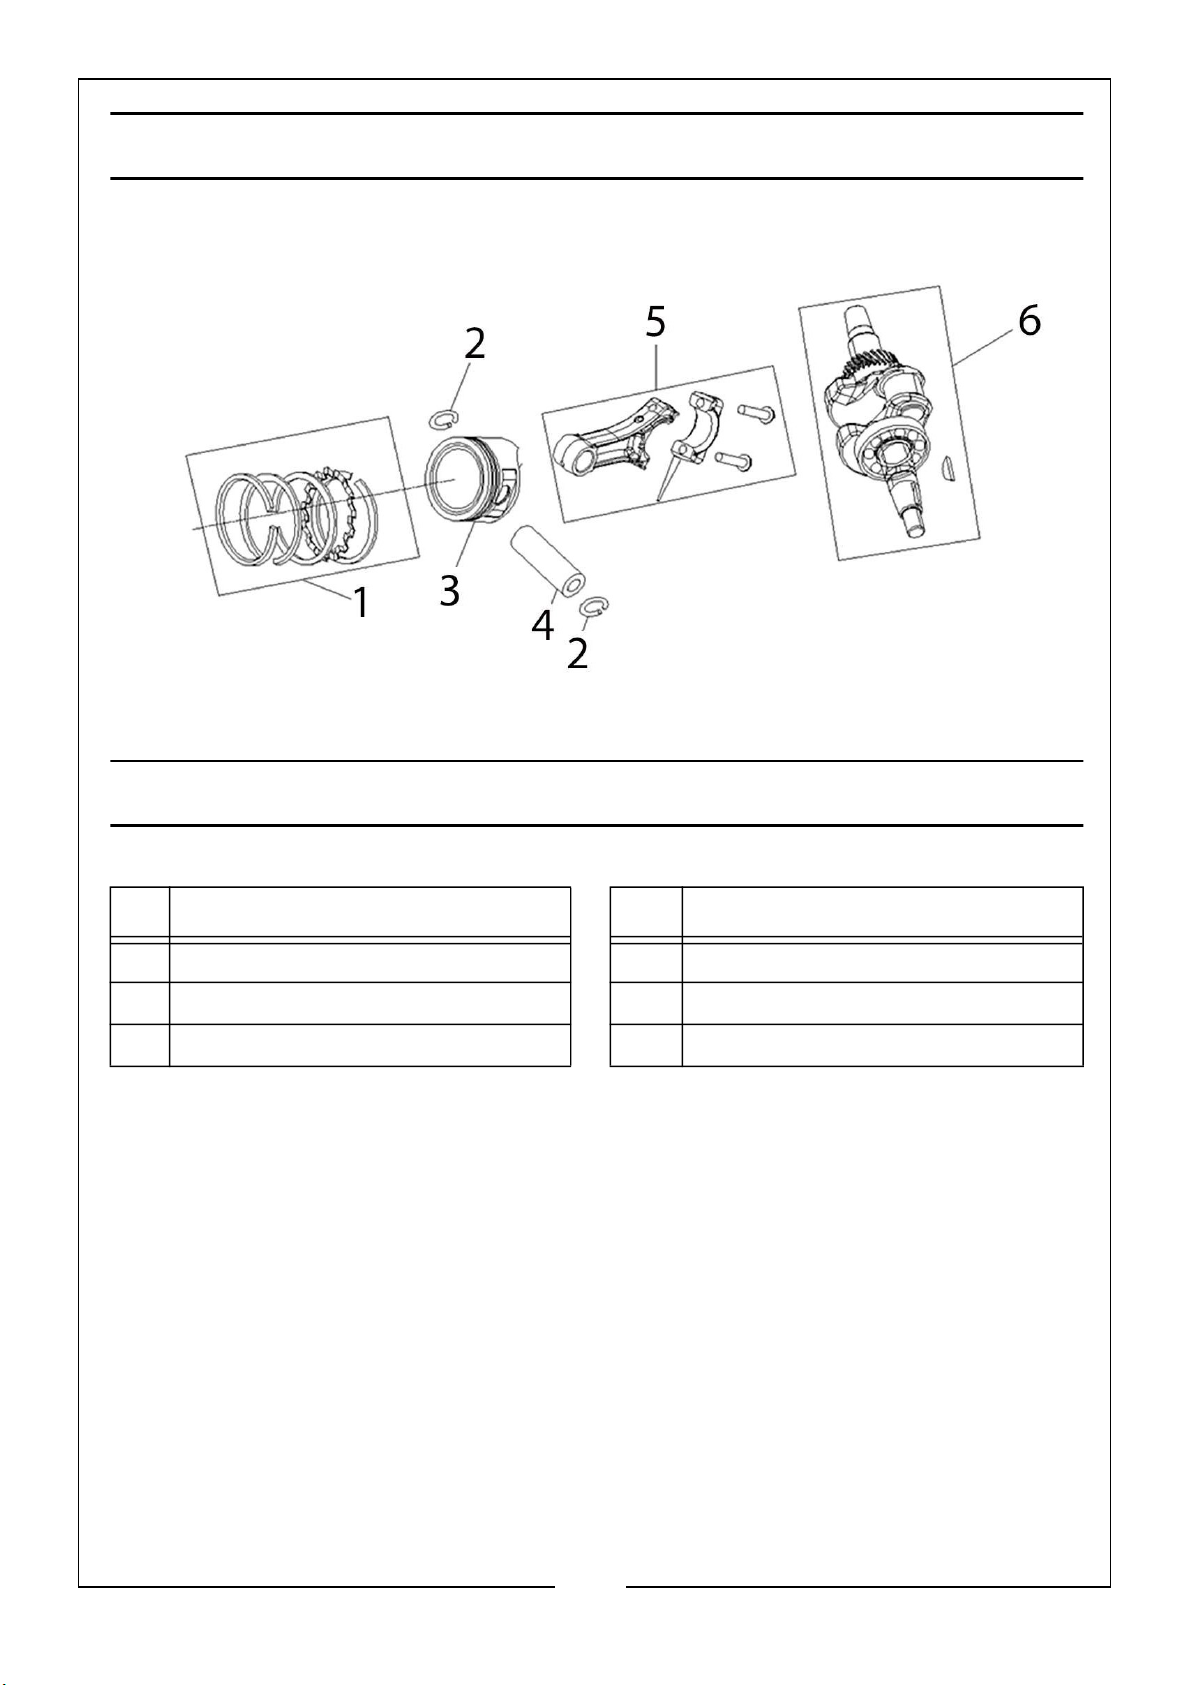
EXPLODED DIAGRAM - CRANKSHAFT PISTON
PARTS LIST - CRANKSHAFT PISTON
NO DESCRIPTION NO DESCRIPTION
1 Ring Set, Piston 4 Piston Pin
2 Piston Pin Clip x 2 5 Connecting Rod Assembly
3 Piston Head 6 Crankshaft Assembly
49
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 50
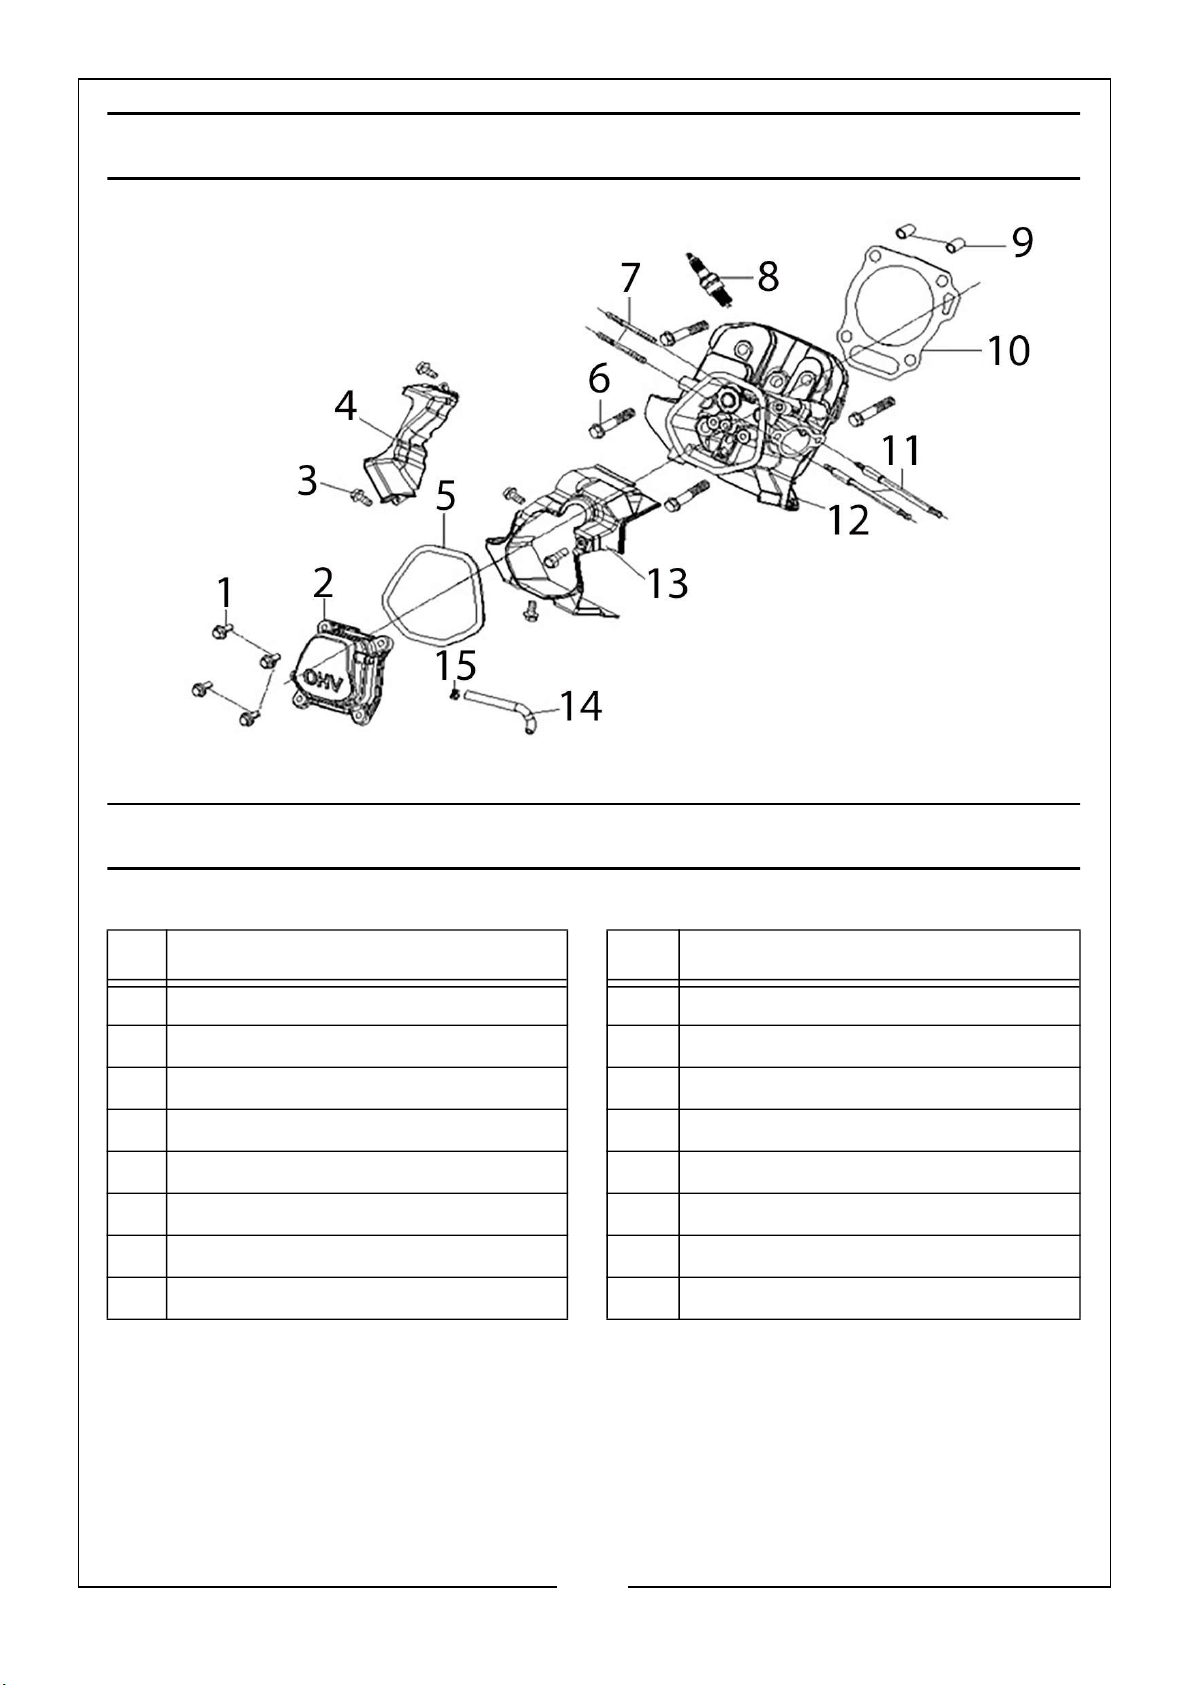
EXPLODED DIAGRAM - CYLINDER HEAD
PARTS LIST - CYLINDER HEAD
NO DESCRIPTION NO DESCRIPTION
1 M6 x 20 Bolt x 4 9 Dowel Pin x 2
2 Cover 10 Gasket Head Cover
3 M6 x 12 Bolt x 5 11 Stud Bolt (Intake) x 2
4 Wind Guider 12 Cylinder Head
5 Gasket Head Cover 13 Shroud
6 Bolt x 4 14 Breather Tube
7 Stud Bolt (Exhaust) x 2 15 Fuel Pipe Clip
8 Spark Plug
50
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 51
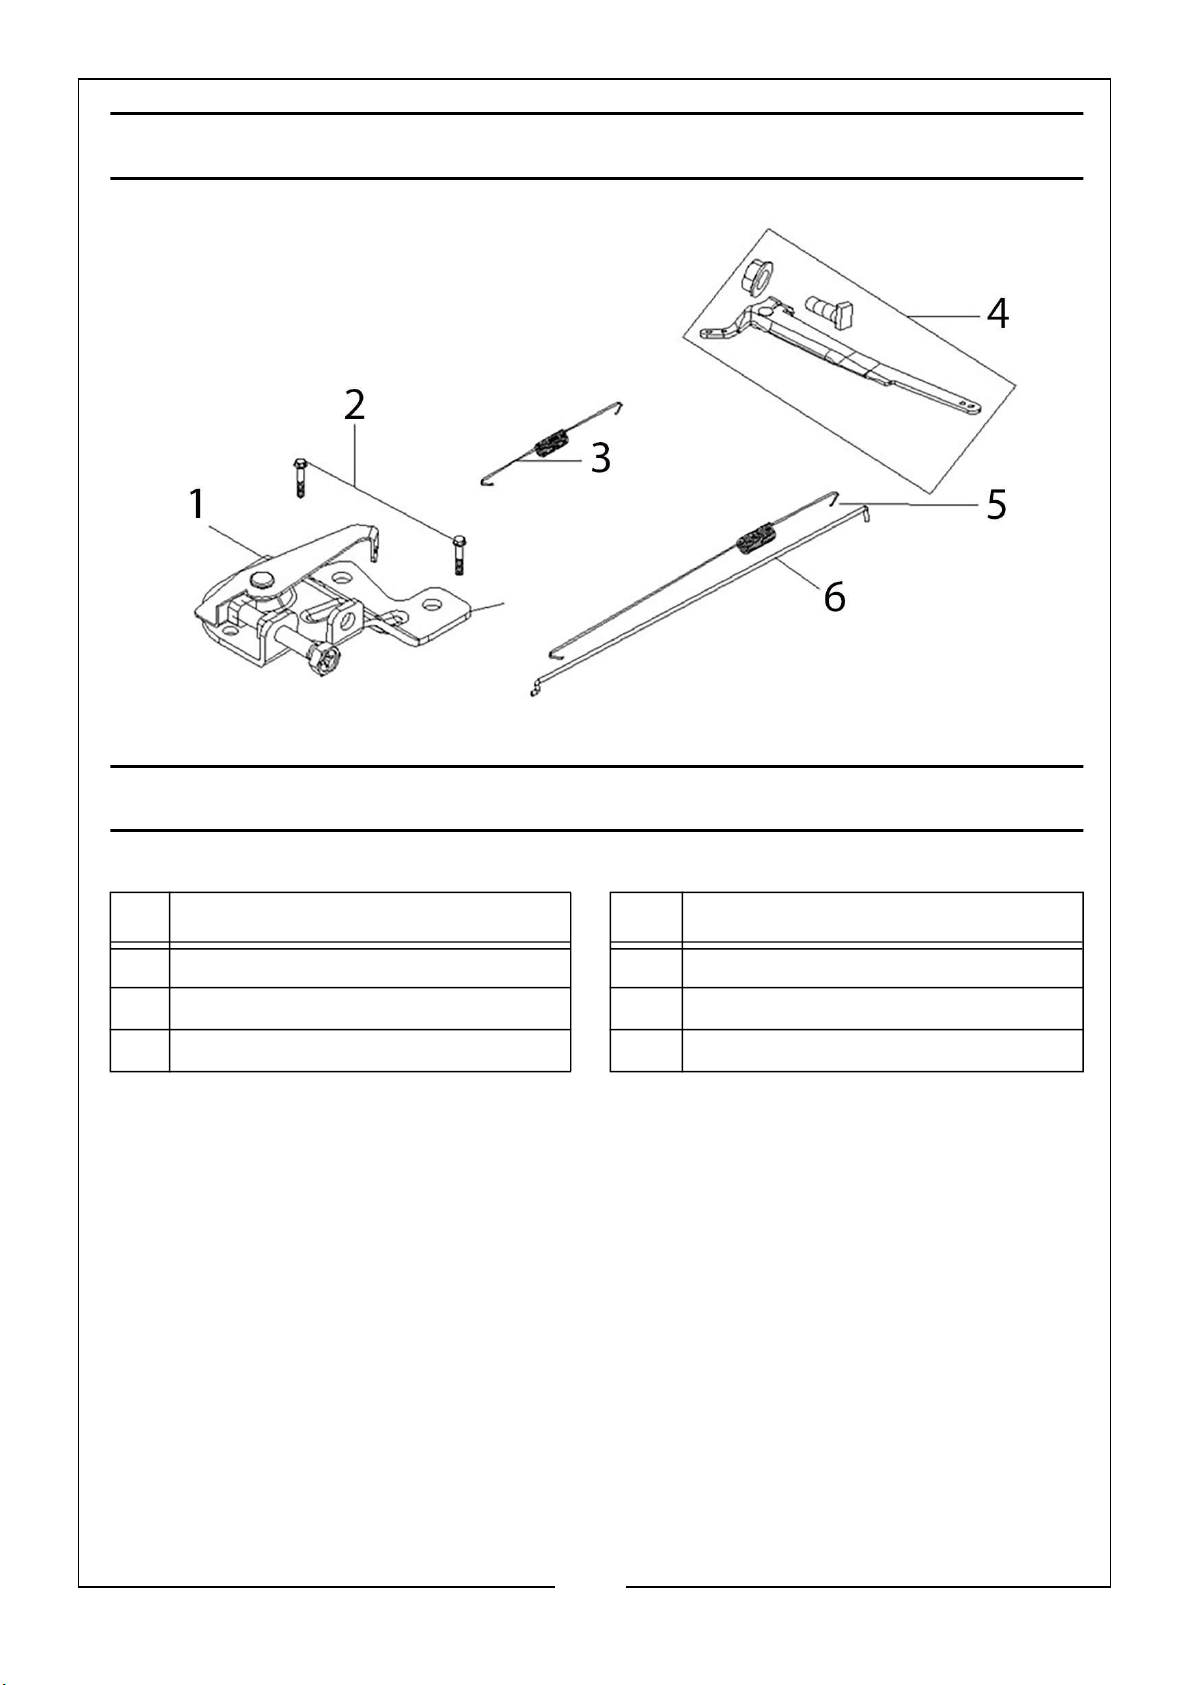
EXPLODED DIAGRAM - ENGINE CONTROLS
PARTS LIST - ENGINE CONTROLS
NO DESCRIPTION NO DESCRIPTION
1 Speed Control Assembly 4 Speed Control Handle Assembly
2 Bolt x 2 5 Throttle Return Spring
3 Cable Return Spring 6 Governor Rod
51
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 52
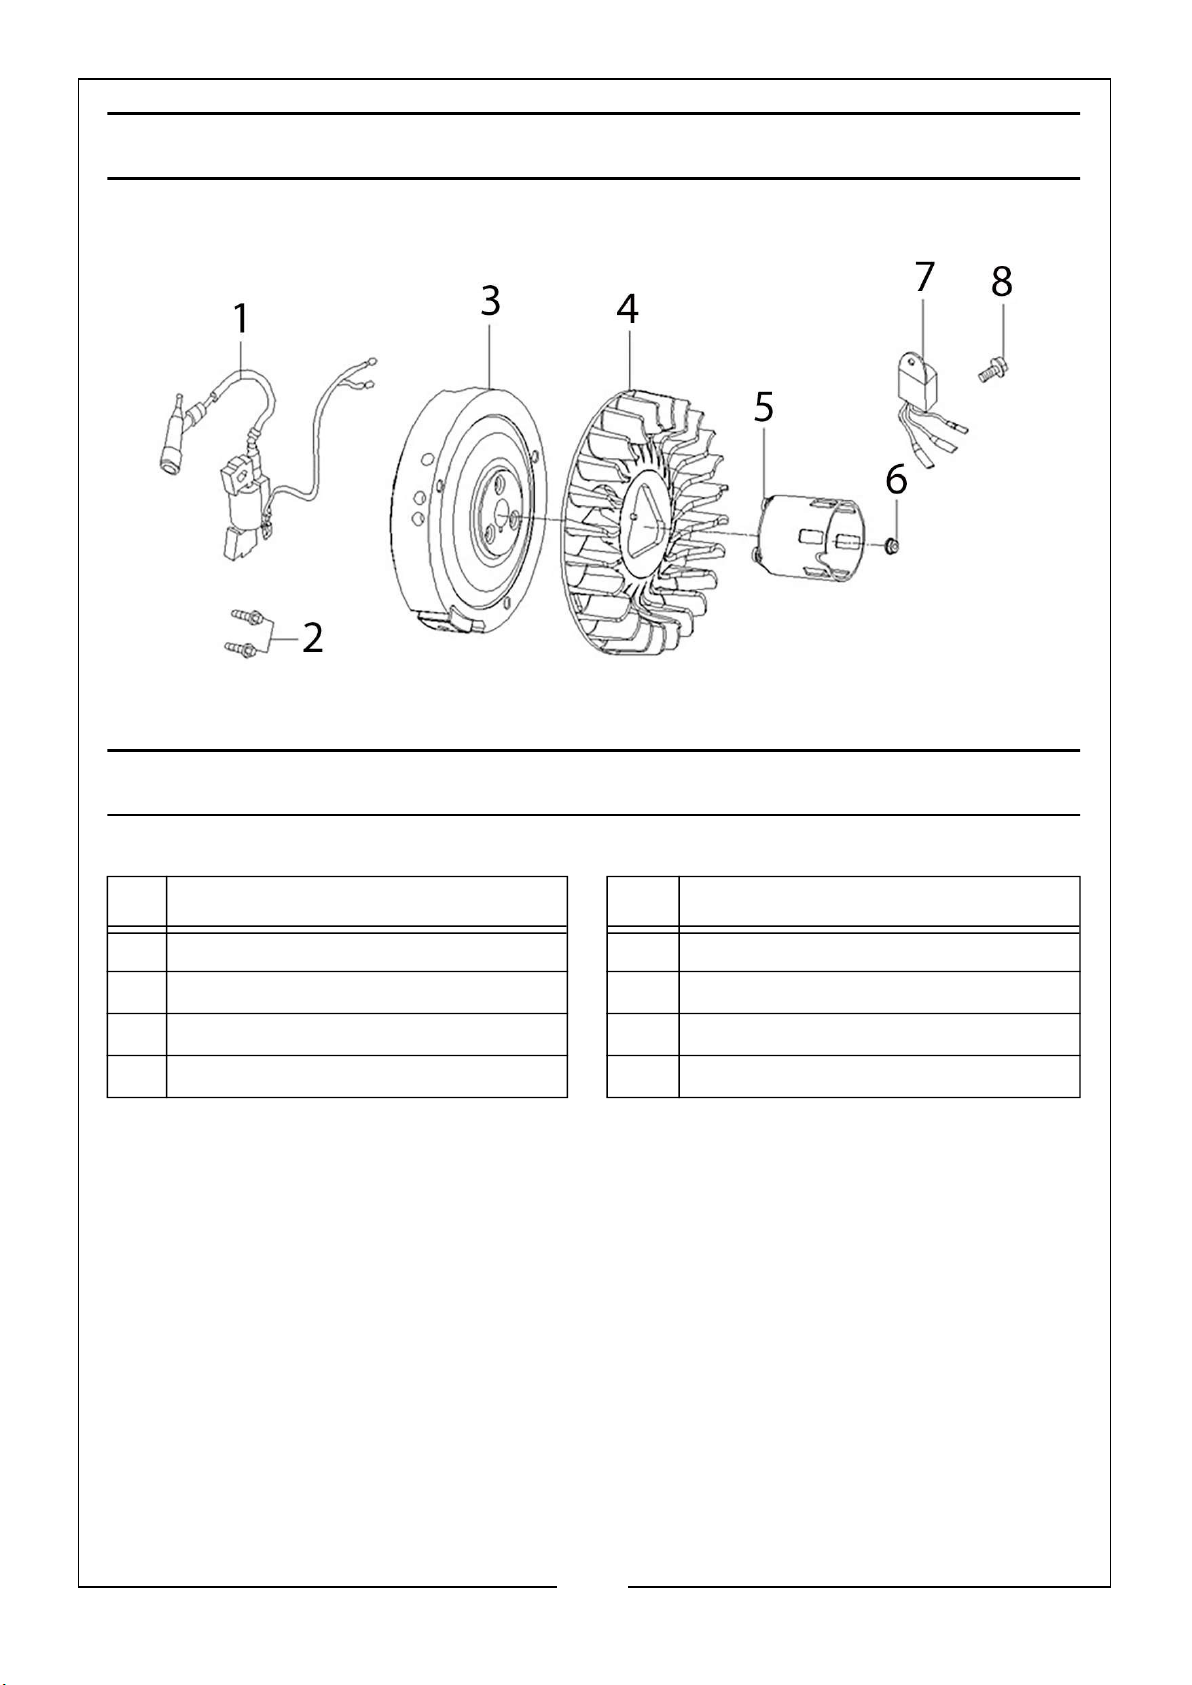
EXPLODED DIAGRAM - FLYWHEEL
PARTS LIST - FLYWHEEL
NO DESCRIPTION NO DESCRIPTION
1 Engine Switch Wire 5 Starter Pulley
2 Flange Bolt x 2 6 Nut
3 Flywheel 7 Oil Alarm
4 Cooling Fan 8 Flange Bolt
52
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 53
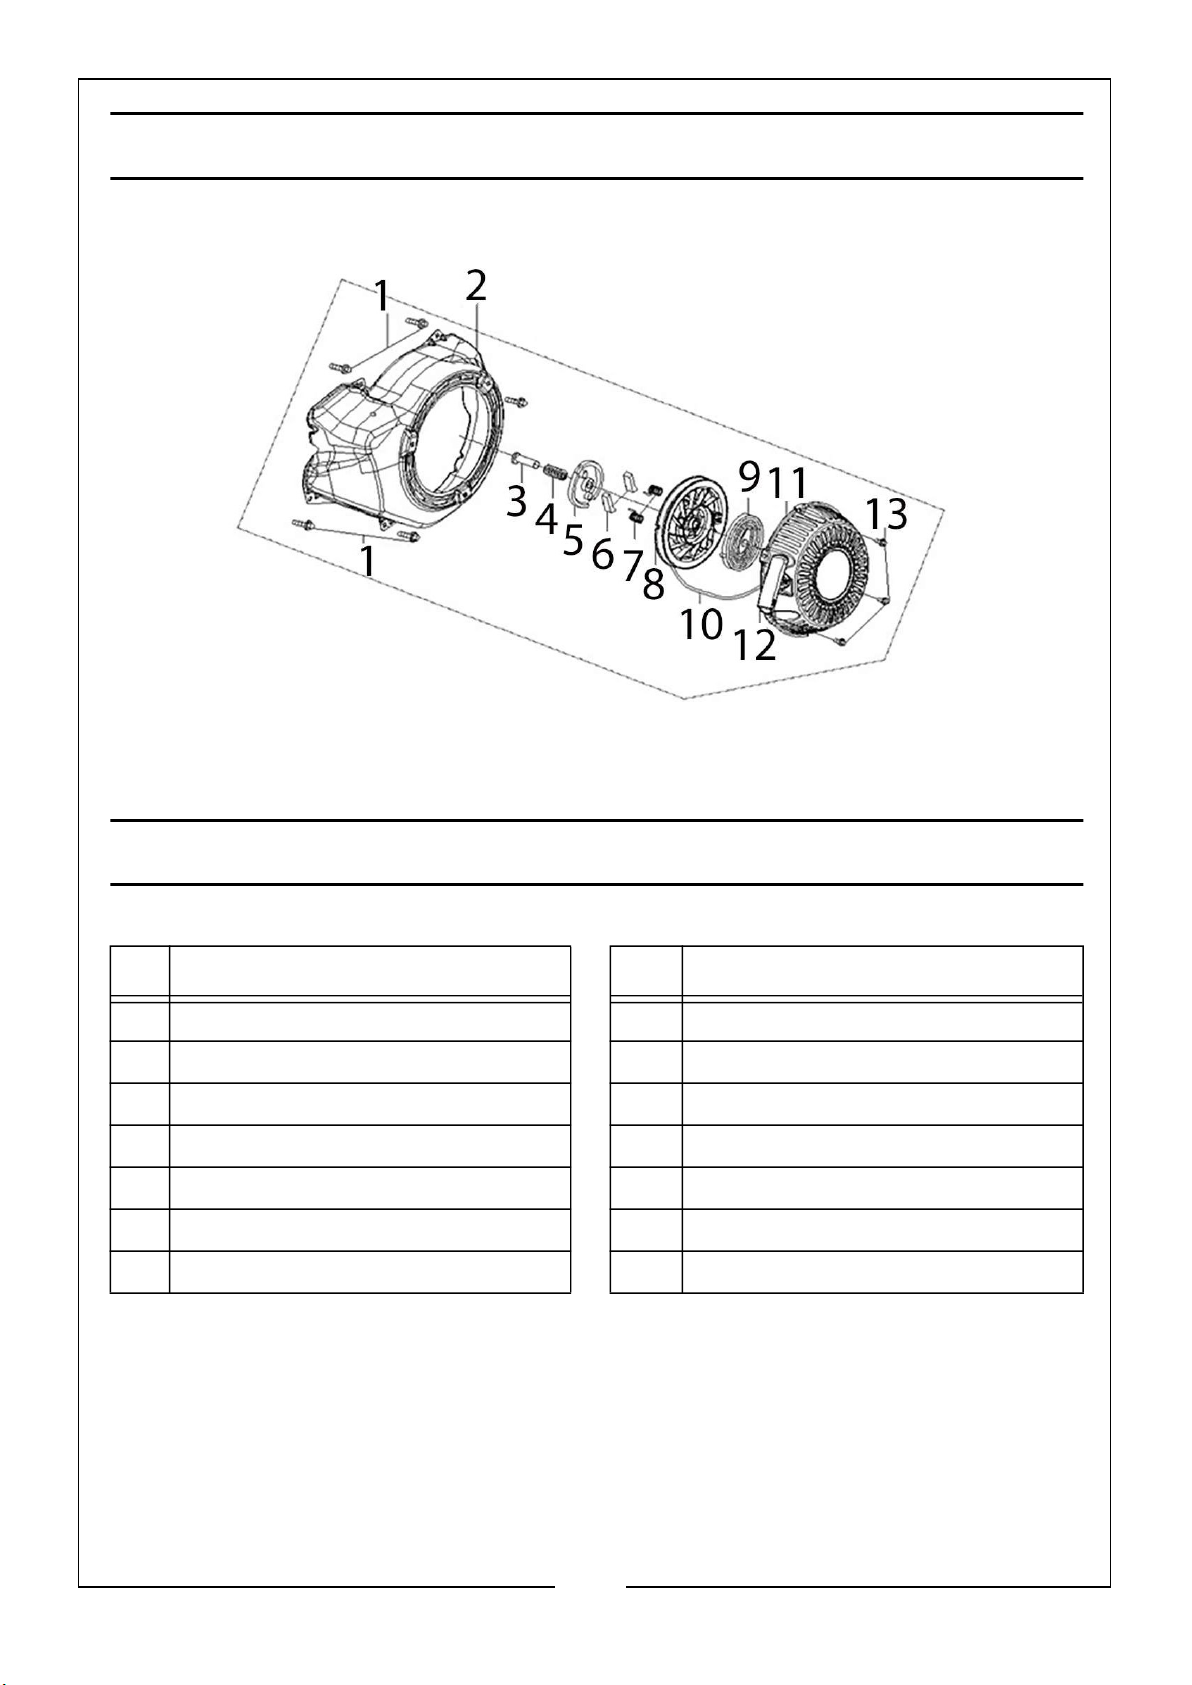
EXPLODED DIAGRAM - RECOIL STARTER
PARTS LIST - RECOIL STARTER
NO DESCRIPTION NO DESCRIPTION
1 M6 x 12 Bolt x 5 8 Recoil Starter Reel
2 Recoil Wind Guilder 9 Recoil Starter Spring
3 Setting Screw 10 Recoil Starter Rope
4 Friction Spring 11 Cover
5 Ratchet Guide 12 Recoil Starter Handle
6 Starter Ratchet x 2 13 Flange Bolt x 3
7 Return Spring x 2
53
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 54
Page 55
DECLARATION OF CONFORMITY
55
Parts & Service: 020 8988 7400 / E-mail: [email protected] or [email protected]
Page 56
 Loading...