

Carver Pump RSA, RS Series, RSB, RSC, RSE Installation, Operation And Maintenance Instructions
...Page 1
Part Number: _______________________________________
Serial Numbers: _____________________________________
These operating instructions contain fundamental information and precautionary notes. Please read the manual
thoroughly prior to installation of unit, electrical connection and commissioning. It is imperative to comply with all
other operating instructions referring to components of individual units.
I-280
280 – 16.03.EN
ATEX
Inch Units
For Units Built After December 2015
RS – Multi-Stage, Centrifugal Pump
INSTALLATION, OPERATION AND
MAINTENANCE INSTRUCTIONS
This manual shall always be kept close to the unit’s location of operation or directly on the pump set.
Page 2

RS – Multi-Stage, I-280
EC Declaration of Conformity
www.carverpump.com
Phone: 1-563-263-3410
Email: [email protected]
Kurt Doren
Quality/ ISO Manager
Centrifugal Pump 280 – 16.03.EN
MANUFACTURER: CARVER PUMP COMPANY
2415 PARK AVE.
MUSCATINE, IOWA, USA 52761
PRODUCT DESCRIPTION: RS – Multi-Stage, Centrifugal Pump
PART NUMBER:
SERIAL NUMBER:
DATE MANUFACTURED:
APPLICABLE EUROPEAN DIRECTIVES:
Machinery: The designated product complies with the following basic requirements of Directive 2006/42/EC:
Appendix I, section 1.1.2, 1.1.3., 1.1.5., 1.3.1., 1.3.2., 1.3.3., 1.3.4., 1.3.7., 1.3.8., 1.4.1., 1.4.2.1.,
1.5.1., 1.5.8., 1.5.9., 1.5.13., 1.6.1., 1.6.4., 1.6.5., 1.7.
ATEX: 94/9/EC
APPLICABLE INTERNATIONAL STANDARDS:
Machinery: EN ISO 12100:2010 EN ISO 13732-1:2008
EN 626-1:2008 EN ISO 13857:2008
ATEX: EN 1127-1, EN 13463-1, EN 13463-5
NOTIFIED BODY
Det Norske Veritas, ATEX NB 0575 retains a copy of the Technical File
ATEX product marking: II 2 G c T2
The product described in this Declaration of Conformity complies with the Applicable European Directives and
relevant sections of the Applicable International Standards. The signature on this document authorizes the distinctive
European mark to be applied to the equipment described. A Technical Construction File is available for inspection by
designated bodies
Authorized Signature: Date:
Important safety information is contained in the installation, operation and service manuals; read and
understand this information prior to installing or using this equipment
This Document applies only to the equipment described above and is invalid if not reproduced in its entirety.
Page 3
RS – Multi-Stage, I-280
Installation Date
Location
Application
Centrifugal Pump 280 – 16.03.EN
SERVICE RECORD PAGE
Service No. ______________________ Model _________________________ Size and Type _______________
Customer Order No. ____________________________ Date Installed __________________________________
PUMP RATING
Capacity _____________________________________ Total Head ____________________________________
Suction Pressure ______________________________ Speed (RPM) __________________________________
Liquid pumped ________________________________ Temperature ___________________________________
Specific Gravity _______________________________ Viscosity ______________________________________
Service ______________________________________
PUMP MATERIALS
Casing _________________________ Impeller _______________________ Shaft _______________________
Gaskets _____________________________________ Bearing Frame _________________________________
Mechanical Seal/Packing ________________________
MOTOR DATA
Motor __________________________ Make _________________________ Serial No. ___________________
Type ___________________________ Frame ________________________ AC or DC ___________________
HP _____________________________ RPM _________________________ Volts _______________________
Phase __________________________ Cycles ________________________
Page 4
RS – Multi-Stage, I-280
INSPECTION DATE
REPAIR TIME
REPAIRS
COST REMARKS
Centrifugal Pump 280 – 16.03.EN
NOTES ON INSPECTION AND REPAIRS
Page 5
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
INSTALLATION, OPERATION AND
MAINTENANCE INSTRUCTIONS
TABLE OF CONTENTS
SECTION/PARAGRAPH PAGE
SECTION/PARAGRAPH PAGE
I. GENERAL DESCRIPTION ............................... 1
A. General Information ................................... 1
B. ATEX Directive 94/9/EC ............................. 1
C. Disclaimer .................................................. 1
D. Personnel Qualification and Training ......... 1
E. Pump Identification..................................... 1
F. Parts Inventory Guide ................................ 2
G. Parts Ordering ............................................ 2
II. SAFETY ............................................................ 2
A. Safety Precautions ..................................... 2
B. Summary of Safety Marking ....................... 2
C. Products Used in Potentially Explosive
Atmospheres ......................................... 2
D. Scope of Compliance ................................. 2
E. Safety Awareness ...................................... 3
F. Safety Instructions for the Operator/User .. 3
G. Safety Instructions for Maintenance
Inspection and Installation Work ............ 3
H. Non-Compliance with Safety Instructions .. 3
I. Unauthorized Modification and
Manufacture of Spare Parts ................... 3
J. Unauthorized Modes of Operation ............. 4
K. Explosion Protection .................................. 4
III. EQUIPMENT DESCRIPTION ........................... 7
IV. EFFECTS OF FLUIDS ..................................... 8
A. Net Positive Suction Head (NPSH) ............ 8
B. Changing Pump Speed .............................. 8
C. Effects of Viscosity ..................................... 8
D. Effects of Specific Gravity .......................... 8
V. TECHNICAL DATA ........................................... 8
VI. INSPECTION AND STORAGE ........................ 16
A. Inspection ................................................... 16
B. Packing for Return ..................................... 16
C. Storage of Pump ........................................ 16
VII. INSTALLATION ................................................ 17
A. Location ...................................................... 17
B. Handling ..................................................... 17
C. Foundation ................................................. 17
D. Leveling of Unit .......................................... 18
E. Grouting ..................................................... 18
F. Coupling Alignment .................................... 20
G. Pre-Installation Procedures ....................... 21
H. Piping ......................................................... 21
I. Auxiliary Piping Connection
and Gauges ........................................... 21
J. Motor .......................................................... 21
K. Direction of Rotation .................................. 21
VIII. OPERATION .................................................... 22
A. Pre-Start Cautions ..................................... 22
B. Priming ....................................................... 22
C. Starting the Pump ...................................... 23
D. Turbine Applications .................................. 23
E. Minimum/Maximum Flow Calculations ...... 23
F. Operating Checks ...................................... 23
G. Stopping the Pump .................................... 23
H. Indefinite Shutdown ................................... 24
IX. TROUBLESHOOTING OPERATING
PROBLEMS ...................................................... 24
X. MAINTENANCE ............................................... 26
A. Lubrication of Pump Bearings .................... 26
B. Lubrication of Motor Bearings .................... 27
C. Torque Values ............................................ 27
XI. SERVICE AND REPAIR ................................... 28
A. Preparations for Disassembly of Pump ..... 28
B. Disassembly of Pump with
Standard Sleeve Bearing ....................... 29
C. Disassembly of Pump with
Optional Mechanical Seals .................... 31
D. Parts Inspection ......................................... 33
E. Reassembly of Pump with
Standard Sleeve Bearing ....................... 35
F. Reassembly of Pump with
Optional Mechanical Seals .................... 39
G. Replacement of Wear Ring ........................ 42
H. Motor .......................................................... 44
I. Check Valve ............................................... 44
XII. PARTS LISTS AND DRAWINGS ..................... 44
Page 6
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
TABLE OF CONTENTS - Continued
LIST OF TABLES
NUMBER TITLE PAGE
1. Fluid Temperature Limits ........................... 5
2. Maximum Allowable Pressures .................. 6
3. Axial Impeller Alignment
Control Dimensions................................ 9
4. Shaft Dimensions ....................................... 12
5. Sleeve Bearing Dimensions ....................... 12
6. Standard Design Pump Mechanical
Seal Settings .......................................... 12
7. Optional Design Pump Mechanical
Seal Settings .......................................... 13
8. Key Mechanical Data ................................. 13
9. Permissible Nozzle Loads ......................... 15
10. Minimum Flow Rates RS-6 and RS-9 ........ 15
11. Pumping Unit Troubleshooting .................. 24
12. Oil Recommendations................................ 27
13. Bearing Cooling Flow Rates
(30 PSIG Max.) ...................................... 27
14. Recommended Torque Values (ft-lbs) ....... 27
15. Recommended Equipment ........................ 27
16. Factory Wear Ring Clearance (Inches) ..... 34
17. New Wear Ring Diametrical
Clearance Limits (Inches) ...................... 43
18. Recommended Spare Parts List ................ 45
LIST OF ILLUSTRATIONS
NUMBER TITLE PAGE
1. Seal Chamber Dimensions .........................11
2. Standard Seal Flush Plans .........................13
3. Bearing Frame Water Cooling ....................14
4. Sling Position for Moving Pump ..................17
5. Sling Position for Moving Pumping Unit .....17
6. Sling Position for Moving
Pumping Unit with Lifting Lugs ...............17
7. Grouting and Foundation Bolting ................19
8. Unit Leveling ...............................................19
9. Coupling Alignment .....................................20
10. Constant Level Oiler ...................................27
11. Bushing Not Torqued Interference .............38
12. Mechanical Seal Not Torqued
Interference .................................................42
13. Sectional Assembly – Standard
Sleeve Bearing .......................................49
14. Sectional Assembly – Optional
Mechanical Seals ....................................51
15. Cooling Options ..........................................52
Page 7
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
I. GENERAL DESCRIPTION AND
SAFETY PRECAUTIONS.
A. GENERAL INFORMATION. Carver Pump
Company products are carefully engineered and
manufactured and, if properly installed, maintained, and
operated, should provide maintenance-free operation
and a long service life.
CAUTION
These instructions must always be kept close
to the product's operating location or directly
with the product.
This manual is designed to provide sufficient material to
properly maintain the total pumping unit. The information
presented should improve your knowledge and
understanding of the RS Multi-Stage Centrifugal Pump,
thus upgrading the reliability, service life, and quality of
pump maintenance.
These operating instructions are intended to facilitate
familiarization with the product and its permitted use to
help satisfy ATEX safety requirements. These operating
instructions do not take into account local regulations;
the operator must ensure that such regulations are
strictly observed by all, including the personnel called in
for installation. Compliance with such laws relating to
the proper installation and safe operation of the pumping
equipment is the responsibility of the equipment owner
and all necessary steps should be taken by the owner to
assure compliance with such laws before operating the
equipment. These instructions are intended to facilitate
familiarization with the product and its permitted use to
help satisfy safety requirements. Always coordinate
repair activity with operations personnel, and follow all
plant safety requirements and applicable safety and
health laws/regulations.
Refer to Figures 13, 14, and 15 to locate the pump parts
by item number. Variations do exist between
configurations, not all parts described in the text may be
on your configuration.
CAUTION
These instructions should be read prior to
installing, operating, using and maintaining the
equipment in any region worldwide and in
conjunction with the main user instructions
provided. The equipment must not be put into
service until all the conditions relating to safety
instructions have been met.
B. ATEX DIRECTIVE 94/9/EC. It is a legal
requirement that machinery and equipment put into
service within certain regions of the world shall conform
to the applicable CE Marking Directives for Equipment
for Potentially Explosive Atmospheres (ATEX).
Where applicable the Directive covers important safety
aspects relating to the equipment, its use and the
satisfactory provision of technical documents. Where
applicable this document incorporates information
relevant to these Directives. To establish if the product
itself is CE marked for a Potentially Explosive
Atmosphere check the nameplate and the Certification
provided.
C. DISCLAIMER. Information in these User
Instructions is believed to be reliable. In spite of all the
efforts of Carver Pump Company to provide sound and
all necessary information the content of this manual may
appear insufficient and is not guaranteed by Carver
Pump Company as to its completeness or accuracy.
D. PERSONNEL QUALIFICATION AND TRAINING.
All personnel involved in the operation, installation,
inspection and maintenance of the unit must be qualified
to carry out the work involved. If the personnel in
question do not already possess the necessary
knowledge and skill, appropriate training and instruction
must be provided. If required the operator may
commission the manufacturer/supplier to provide
applicable training.
Follow instructions in this manual carefully. Factory
warranty applies only when pump operates under
conditions as specified on order acknowledgment, and if
pump is properly installed and maintained as
recommended herein. A copy of this manual should be
available to operating personnel. Additional copies of
this manual are available upon request from Carver
Pump Company and your local distributor. For
comments and/or questions about information provided,
please contact Carver Pump Company or your local
distributor.
E. PUMP IDENTIFICATION. The type of pump, pump
size, operating data, and serial number are all stamped
on the nameplate attached to the pump. Pump
specifications should be recorded upon receipt of the
pumping unit. Record all necessary information on the
pump service record page and inspection and repair
record provided at the front of this manual. This
information must be included in all correspondence
regarding the unit. This will ensure that the correct pump
and/or parts are ordered in a timely manner.
1
Page 8

RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
F. PARTS INVENTORY GUIDE. To avoid
unnecessary delays for maintenance, spare parts
should be readily available, purchase before and keep in
used in safety instructions where noncompliance in the hazardous area would cause
the risk of an explosion.
stock, for normal service. Most conditions will be
covered if this manual is followed. For every one to
three pumps, stock one spare set consisting of items
listed in Table 19, Recommended Spare Parts. Part
General hazard sign to ISO 7000 - 0434.
numbers correspond to Figures 11, 12 and 13.
The word "Caution" is used to introduce safety
G. PARTS ORDERING. When ordering replacement
parts, please specify:
instructions whose non-observance may lead to damage
to the machine and its functions.
Instructions attached directly to the machine, e.g.
Serial number of pump (located on nameplate)
Part name (located on parts list)
Quantity of parts needed
Carver Pump Company may ship an interchangeable
part that is not identical in appearance or symbol. This is
done only if the part has been improved. Examine parts
carefully upon delivery before questioning factory or
Arrow indicating the direction of rotation
Markings for fluid connections must always be
complied with and be kept in a perfectly legible
condition at all times.
Observe all notes, caution or danger tags attached to
the equipment or included in this manual.
company representative. Never return parts to the
factory without authorization from Carver Pump
Company.
C. PRODUCTS USED IN POTENTIALLY EXPLOSIVE
ATMOSPHERES
If an impeller is ordered, specify diameter across blade
tips. Be sure diameter was NOT trimmed further than
diameter shown on Carver Pump Company records.
If a driver or driver parts are ordered, specify name of
manufacturer and all other data found on the driver
nameplate.
II. SAFETY.
A. SAFETY PRECAUTIONS. The manual is designed
to provide adequate instructions for the safe and
efficient installation, operation, or maintenance of the
pump. Failure or neglect to properly install, operate, or
maintain the pump may result in personal injury,
property damage, or unnecessary damage to the pump.
This manual must be read and understood both by the
installing personnel and the responsible trained
personnel/operators prior to installation and operation,
and it must always be kept close to the location of the
pumping unit for easy access.
B. SUMMARY OF SAFETY MARKING. The safety
instructions contained in this manual follow specific
ATEX safety marking where non-observance of the
instruction will cause a hazard is specially marked with
the symbol:
Measures are required to:
Avoid excess temperature
Prevent buildup of explosive mixtures
Prevent the generation of sparks
Prevent leakages
Maintain the pump to avoid hazard
The following instructions for pumps and pump units
when installed in potentially explosive atmospheres
must be followed to help ensure explosion protection.
Both electrical and non-electrical equipment must meet
the requirements of European Directive 94/9/EC.
D. SCOPE OF COMPLIANCE.
Use equipment only in the zone for which
it is appropriate. Always check that the driver,
drive coupling assembly, seal and pump
equipment are suitably rated and/or certified for
the classification of the specific atmosphere in
which they are to be installed.
This symbol indicates explosive
atmosphere marking according to ATEX. It is
2
Where Carver Pump has supplied only the bare shaft
pump, the Ex rating applies only to the pump. The party
responsible for assembling the pump set shall select the
Page 9
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
coupling, driver, seal and any additional equipment, with
the necessary CE Certificate/Declaration of Conformity
establishing it is suitable for the area in which it is to be
installed.
The output from a variable frequency drive (VFD) can
cause additional heating affects in the motor and so, for
G. SAFETY INSTRUCTIONS FOR MAINTENANCE,
INSPECTION AND INSTALLATION WORK. The
operator is responsible for ensuring that all
maintenance, inspection and installation work be
performed by authorized, qualified personnel who are
thoroughly familiar with the manual and pumping unit.
pump sets with a VFD, the ATEX Certification for the
motor must state that it covers the situation where
electrical supply is from the VFD. This is particular
requirement still applies even if the VFD is in a safe
area.
To ensure safe operation the ball
bearings must be replaced at 20000 hours of
service or whenever the mechanical seal is
inspected or serviced.
E. SAFETY AWARENESS. It is imperative to comply
with the safety instructions contained in this manual, the
relevant national and international explosion protection
regulations, health and safety regulations and the
operator’s own internal work, operation and safety
regulations.
Ex symbol relates to additional
requirements which must be adhered to when
the pump is operated in potentially explosive
atmospheres.
F. SAFETY INSTRUCTIONS FOR THE OPERATOR
/USER.
Any hot or cold components that could pose a
hazard must be equipped with a guard by the
operator.
Guards which are fitted to prevent accidental
contact with moving parts (e.g. coupling) must
not be removed whilst the unit is operating.
Leakages (e.g. at the shaft seal) of hazardous
fluids (e.g. explosive, toxic, hot) must be
contained so as to avoid any danger to persons
or the environment. Pertinent legal provisions
must be adhered to.
The pumping unit must have cooled down to ambient
temperature, pump pressure must have been released
and the pump must have been drained before working
on any pumping unit. Work on the pumping unit must be
carried out during shutdown. The shutdown procedure
described in the manual for taking the unit out of service
must be adhered to.
Pumps handling fluids that are hazardous to personnel
must be decontaminated prior to being worked on.
Immediately following completion of the work, all safety
relevant and protective devices must be reinstalled
and/or reactivated. Please observe all instructions set
out in the Section VIII on start up before returning the
pumping unit to service.
H. NON-COMPLIANCE WITH SAFETY
INSTRUCTIONS. Non-compliance with safety
instructions may result in personal injury, property
damage, or unnecessary damage to the pumping unit.
Non-compliance with these safety instructions will also
lead to forfeiture of any and all rights to claims for
damages. Non-compliance, can for example, result in:
Failure of important pumping unit functions.
Failure of prescribed maintenance and servicing
practices.
Electrical hazards must be eliminated. (In this
respect refer to the relevant safety regulations
applicable to different countries and/or the local
energy supply companies.)
If the pumps/units are located in
potentially explosive atmospheres, it is
imperative to make sure that unauthorized
modes of operation are prevented. Noncompliance may result in the specified
temperature limits being exceeded.
Hazard to personnel by electrical, mechanical,
and chemical effects as well as explosion.
Hazard to the environment due to leakage of
hazardous substances.
I. UNAUTHORIZED MODIFICATION AND
MANUFACTURE OF SPARE PARTS. Modifications or
alterations of the pumping unit supplied are only
permitted after consultation with Carver Pump and to the
extent permitted by Carver Pump. Original spare parts
and accessories authorized by Carver Pump ensure
safety. The use of other parts can invalidate any liability
of Carver Pump for consequential damage and/or
warranty.
3
Page 10
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
J. UNAUTHORIZED MODES OF OPERATION. The
warranty relating to operating reliability and safety of the
unit supplied is only valid if the pumping unit is used in
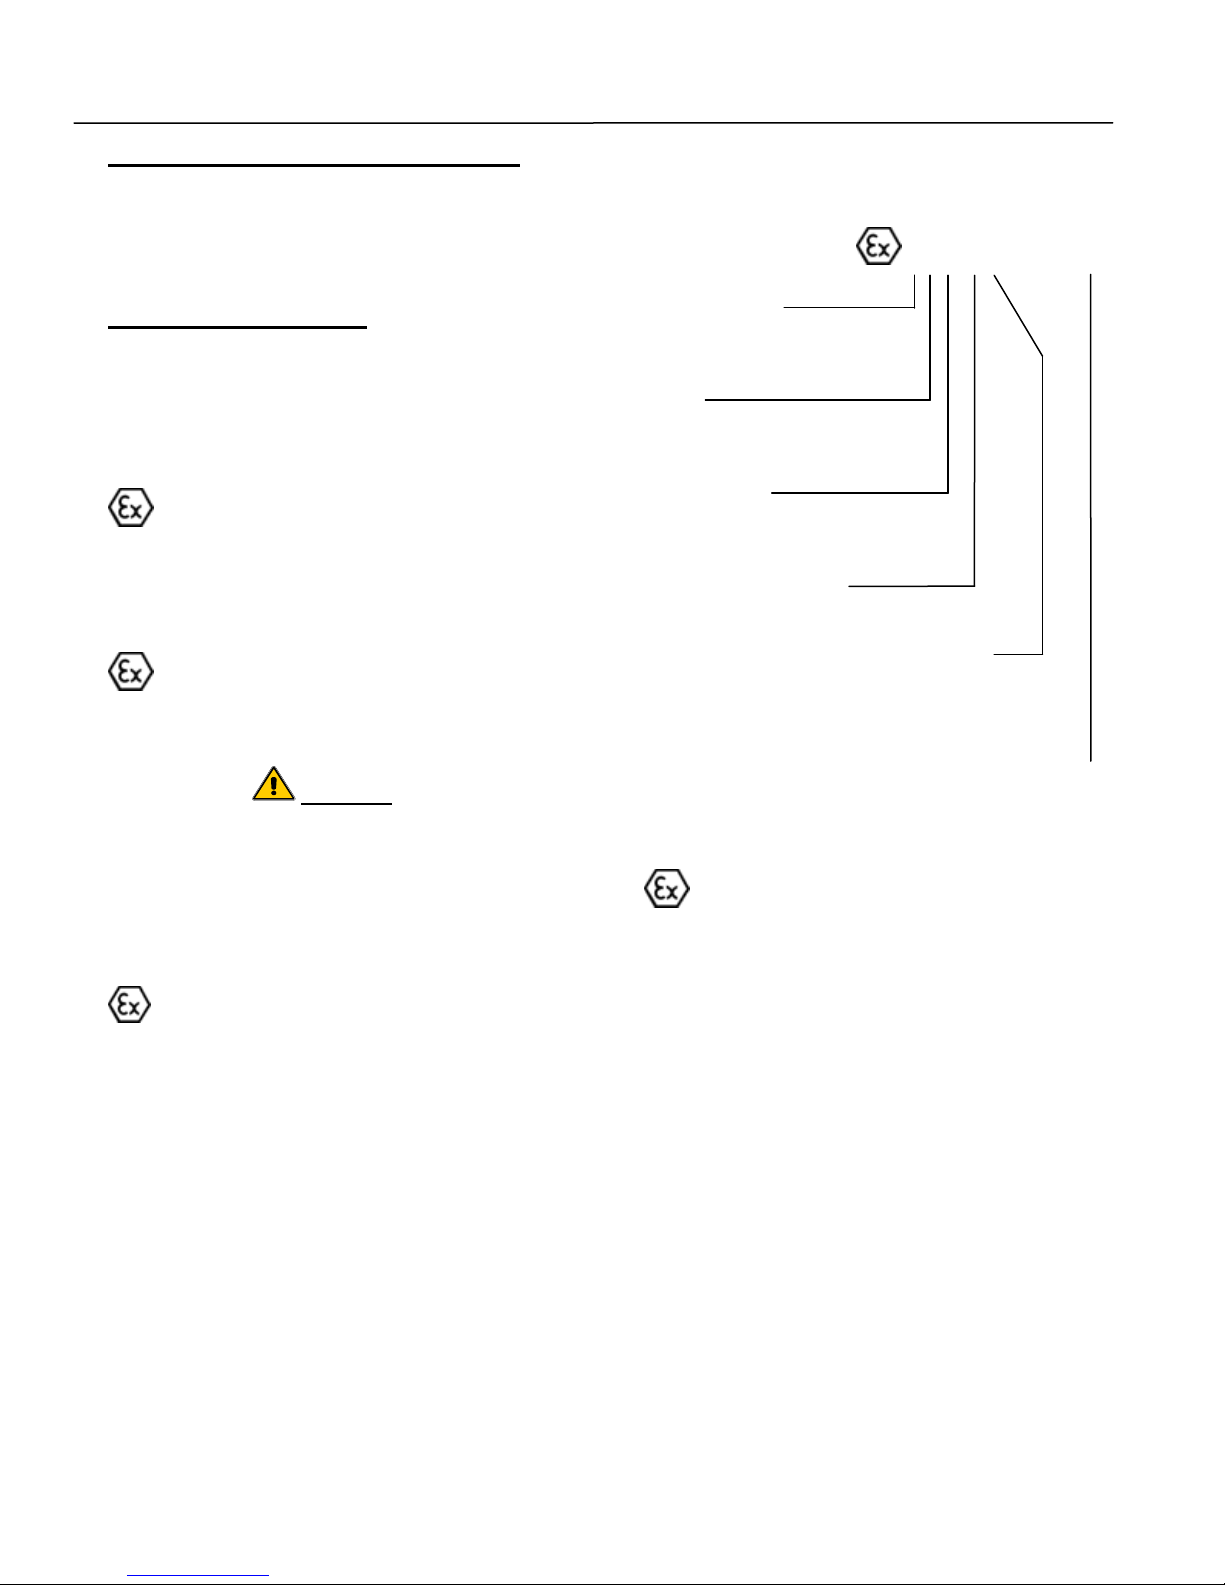
An example of ATEX equipment marking is shown
below. The actual classification of the pump will be
engraved on the nameplate.
accordance with its designated use as described in the
following sections. The limits stated on the nameplate
must not be exceeded under any circumstances.
K. EXPLOSION PROTECTION. If the pumps/units are
installed in potentially explosive atmospheres, the
measures and instructions given in the following
sections K.1 to K.6 must be adhered to without fail, to
ensure explosion protection.
K.1 Unit Fill.
Equipment Group
I = Mining
II = Non-mining
Category
2 or M2 = high level protection
3 = normal level of protection
II 2 GD c IIC 135 ºC (T4)
Gas and/or dust
It is assumed that the system of suction
and discharge lines and thus the wetted pump
G = Gas
D = Dust
internals are completely filled with the fluid to
be handled at all times during pump operation,
so that an explosive atmosphere is prevented.
c = Constructional safety
(in accordance with EN13463-5)
Gas Group (Equipment Category 2 only)
If the operator cannot warrant this
condition, appropriate monitoring devices must
be used.
IIA – Propane (typical)
IIB – Ethylene (typical)
IIC – Hydrogen (typical)
CAUTION
In addition, it is imperative to make sure that
the seal chambers, auxiliary systems of the
shaft seal and the heating and cooling systems
are properly filled.
K.2 Marking.
The marking on the pump only refers to
the pump, i.e. the coupling and driver must be
regarded separately. The coupling must have
an EC manufacturer’s declaration. The driver
must be regarded separately.
Maximum surface temperature (Temperature Class)
(Refer to Section II, Paragraph K.5)
K.3 Checking the Direction of Rotation.
If the explosion hazard also exists during
the installation phase, the direction of rotation
must never be checked by starting up the
unfilled pump unit, even for a short period, to
prevent temperature increases resulting from
contact between rotating and stationary
components.
K.4 Pump Operating Mode.
Make sure that the pump is always started up with the
suction-side shut-off valve fully open and the dischargeside shut-off valve slightly open. However, the pump can
also be started up against a closed swing check valve.
The discharge-side shut-off valve shall be adjusted to
comply with the duty point immediately following the runup process.
4
Page 11
RS – Multi-Stage, I-280
Temperature class
to EN 13463-1:
Temperature limit of
fluid handled
T5
185 °F (85 °C)
T4
284 °F (120 °C)
T3
365 °F (185 °C)
T2
536 °F (280 °C)
T1
662 °F (350 °C)
Centrifugal Pump 280 – 16.03.EN
In the ball bearing bracket area, the unit surfaces must
Pump operation with the shut-off valves in
the suction and/or discharge pipes closed is not
be freely exposed to the atmosphere and the fan inlet
flow must be unimpeded.
permitted.
CAUTION
In this condition, there is a risk of the pump
casing taking on high surface temperatures
after a very short time, due to a rapid
temperature rise in the pumped fluid inside the
pump. Additionally, the resulting rapid pressure
build-up inside the pump may cause excessive
stresses on the pump materials or even
bursting.
The minimum flows calculated in Section VIII,
Paragraph E, refer to water and water-like liquids.
Longer operating periods with these liquids and at the
flow rates indicated will not cause an additional increase
in the temperatures on the pump surface. However, if
the physical properties of the fluids handled are different
from water, it is essential to check if an additional heat
build-up may occur and if the minimum flow rate must
therefore be increased.
To check, proceed as described in Section VIII,
Paragraph E.
In addition, the instructions given in Section VIII of this
operating manual must be observed.
In any case, responsibility for compliance
with the specified fluid temperature (operating
temperature) lies with the plant operator. The
maximum permissible fluid temperature
depends on the temperature class to be
complied with.
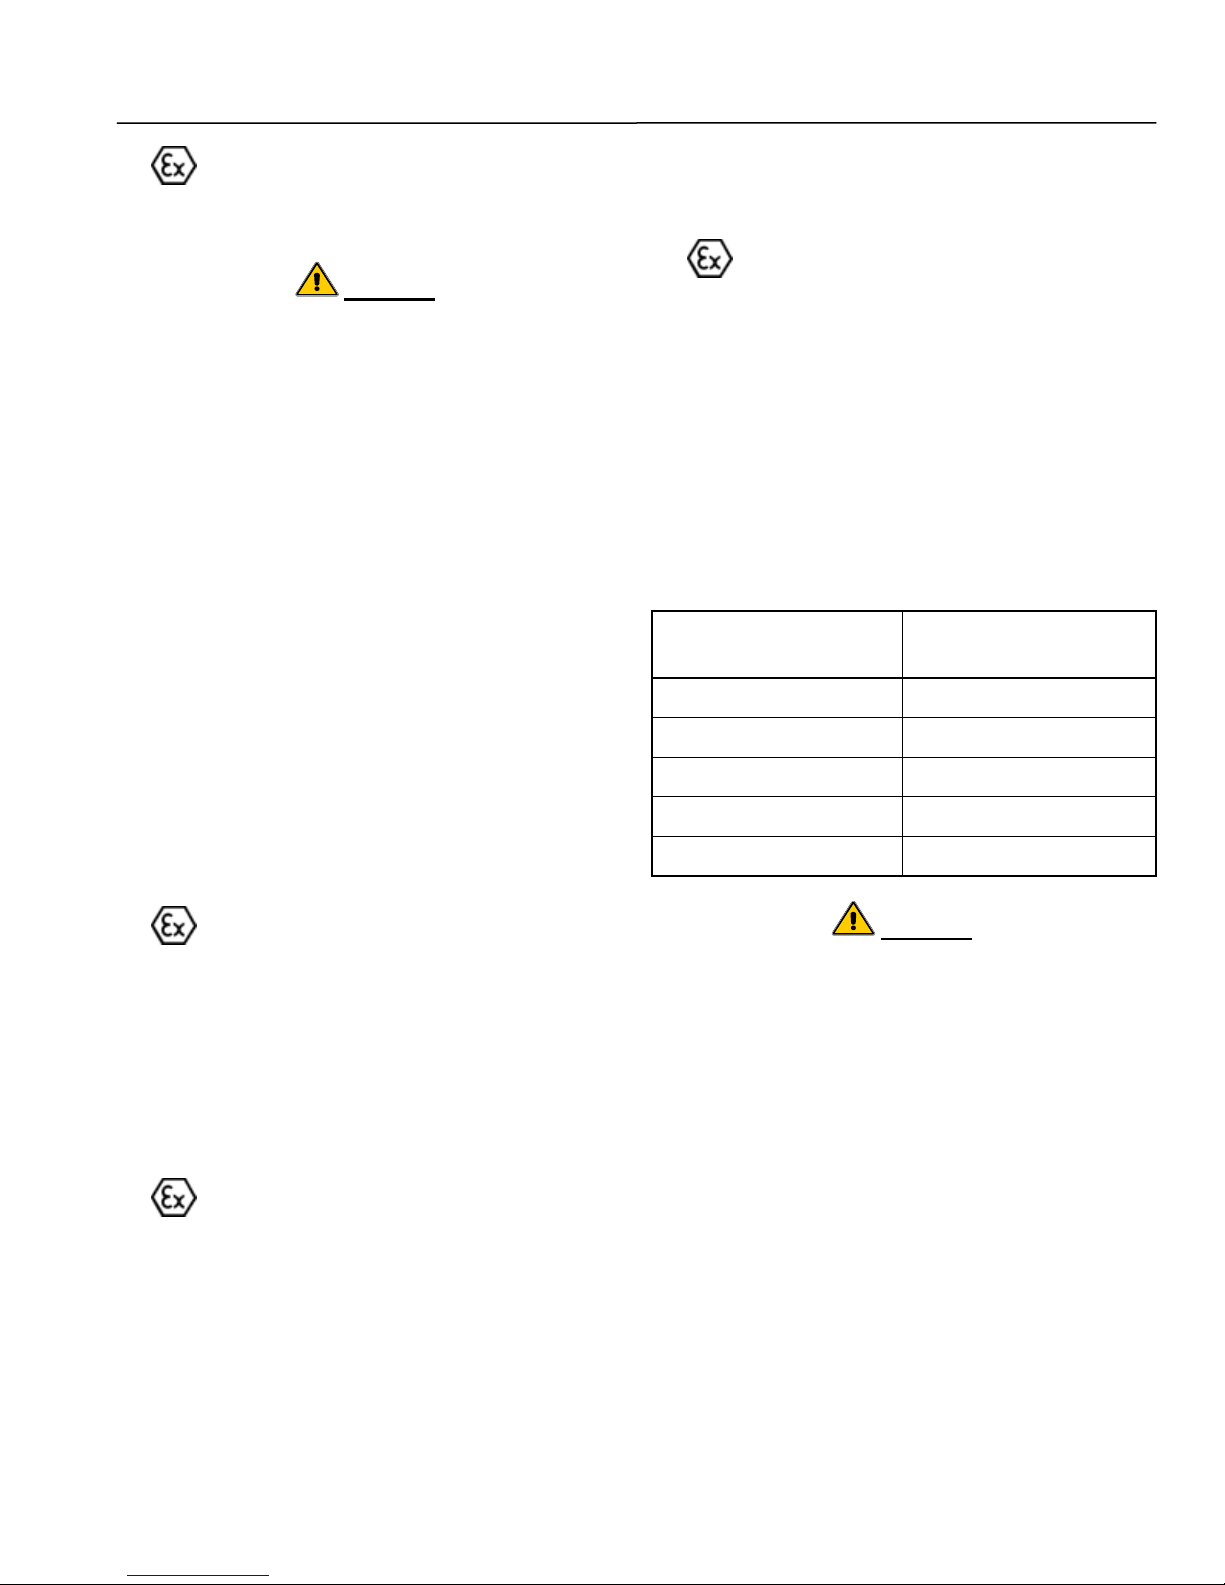
Table 1 below lists the temperature classes to EN
13463-1 and the resulting theoretical temperature limits
of the fluid handled. In stipulating these temperatures,
any temperature rise in the shaft seal area has already
been taken into account.
Table 1. Fluid Temperature Limits
Mechanical seals may exceed the
specified temperature limits if run dry. Dry
running may not only result from an
inadequately filled seal chamber, but also from
excessive gas content in the fluid handled.
Pump operation outside its specified operating range
may also result in dry running.
K.5 Temperature Limits.
In normal pump operation, the highest
temperatures are to be expected on the surface
of the pump casing, at the shaft seal and in the
ball bearing areas. The surface temperature at
the pump casing corresponds to the
temperature of the fluid handled.
If the pump is heated, it must be ensured that the
temperature classes stipulated for the plant are
observed.
CAUTION
The permissible operating temperature of the
pump in question is indicated on the data
sheet. If the pump is to be operated at a higher
temperature, the data sheet is missing or if the
pump is part of a pool of pumps, the maximum
permissible operating temperature must be
enquired from the pump manufacturer.
Based on an ambient temperature of 104˚ Fahrenheit
(F) [40˚ Celsius (C)] and proper maintenance and
operation, compliance with temperature class T4 is
warranted in the area of the rolling element ball
bearings. A special design is required for compliance
with temperature class T6 in the ball bearing area. In
such cases, and if ambient temperature exceeds 104˚F
(40˚C), contact the manufacturer.
5
Page 12
RS – Multi-Stage, I-280
Size
Suction
Discharge
A
415 PSIG*
1,475 PSIG
B
1,475 PSIG
C
1,475 PSIG
D
1,810 PSIG
E
1,460 PSIG
*Unless otherwise rated.
Centrifugal Pump 280 – 16.03.EN
Make sure you are NOT grounded while
Pump liquids over 225˚F (107˚C); pumps
must be equipped with auxiliary cooling.
adjusting electrical equipment or using
measuring equipment.
Pumps of high temperature construction are provided
with cooled ball bearings for a unit operating in
temperature range between 225˚ F and 300˚ F (107˚ C
and 149˚ C). Cooling water flows through cavities of the
bearing frame and keeps temperature of the ball
bearings within acceptable limits. Refer to Table 13 for
cooling flow rates of water temperature of 60˚ F (140˚C)
for ball bearings.
K.6 Maintenance.
Only a pumping unit which is properly
serviced and maintained in perfect technical
condition will give safe and reliable operation.
This also applies to the reliable function of the thrust or
radial ball bearings whose actual lifetime largely
depends on the operating mode and operating
conditions. Regular checks of the lubricant and the
running noises will prevent the risk of excessive
temperatures as a result of the thrust or radial ball
bearings running hot or defective bearing isolators.
The correct function of the bearing isolators must be
checked regularly. Any auxiliary systems installed must
be monitored, as necessary, to make sure that they
function correctly.
In general, use only one hand when servicing
live electrical equipment.
Make sure to de-energize all electrical
equipment before connecting or disconnecting
meters or test leads.
For connecting a meter to terminals for
measurement, use a range higher than the
expected voltage.
Check to make sure that the frame of the driver
and starter panel are securely grounded before
operating pumping unit or performing any tests
or measurements.
If a test meter must be held or adjusted while
voltage is applied, ground case of meter before
starting measurement. DO NOT touch live
equipment while holding the meter. Some
moving vane-type meters should not be
grounded nor held during measurements.
DO NOT use test equipment known to be
damaged or in poor condition.
The following specific safety precautions apply to the
pumping unit:
Hydro suction case separately on RS-9 units.
K.7 General Safety Instructions.
Various federal, state, and local laws affect
installation, use, and operation of pumping
equipment. Compliance with such laws relating
to proper installation and safe operation of
pumping equipment is the responsibility of the
equipment owner.
Prior to working on pump or driver, ensure all
switches and circuit breakers have been locked
in the open (off) position and tagged, “Out of
Service.”
All circuits NOT known to be dead must be
considered live at all times.
DO NOT wear loose or torn clothing around
rotating machines.
While working near electricity, DO NOT use
metal rules, flashlights, metallic pencils, or any
other objects having exposed conducting
material.
Isolate pump for system hydro.
DO NOT exceed maximum rated suction
pressure unless otherwise rated.
DO NOT exceed maximum rated discharge
pressure.
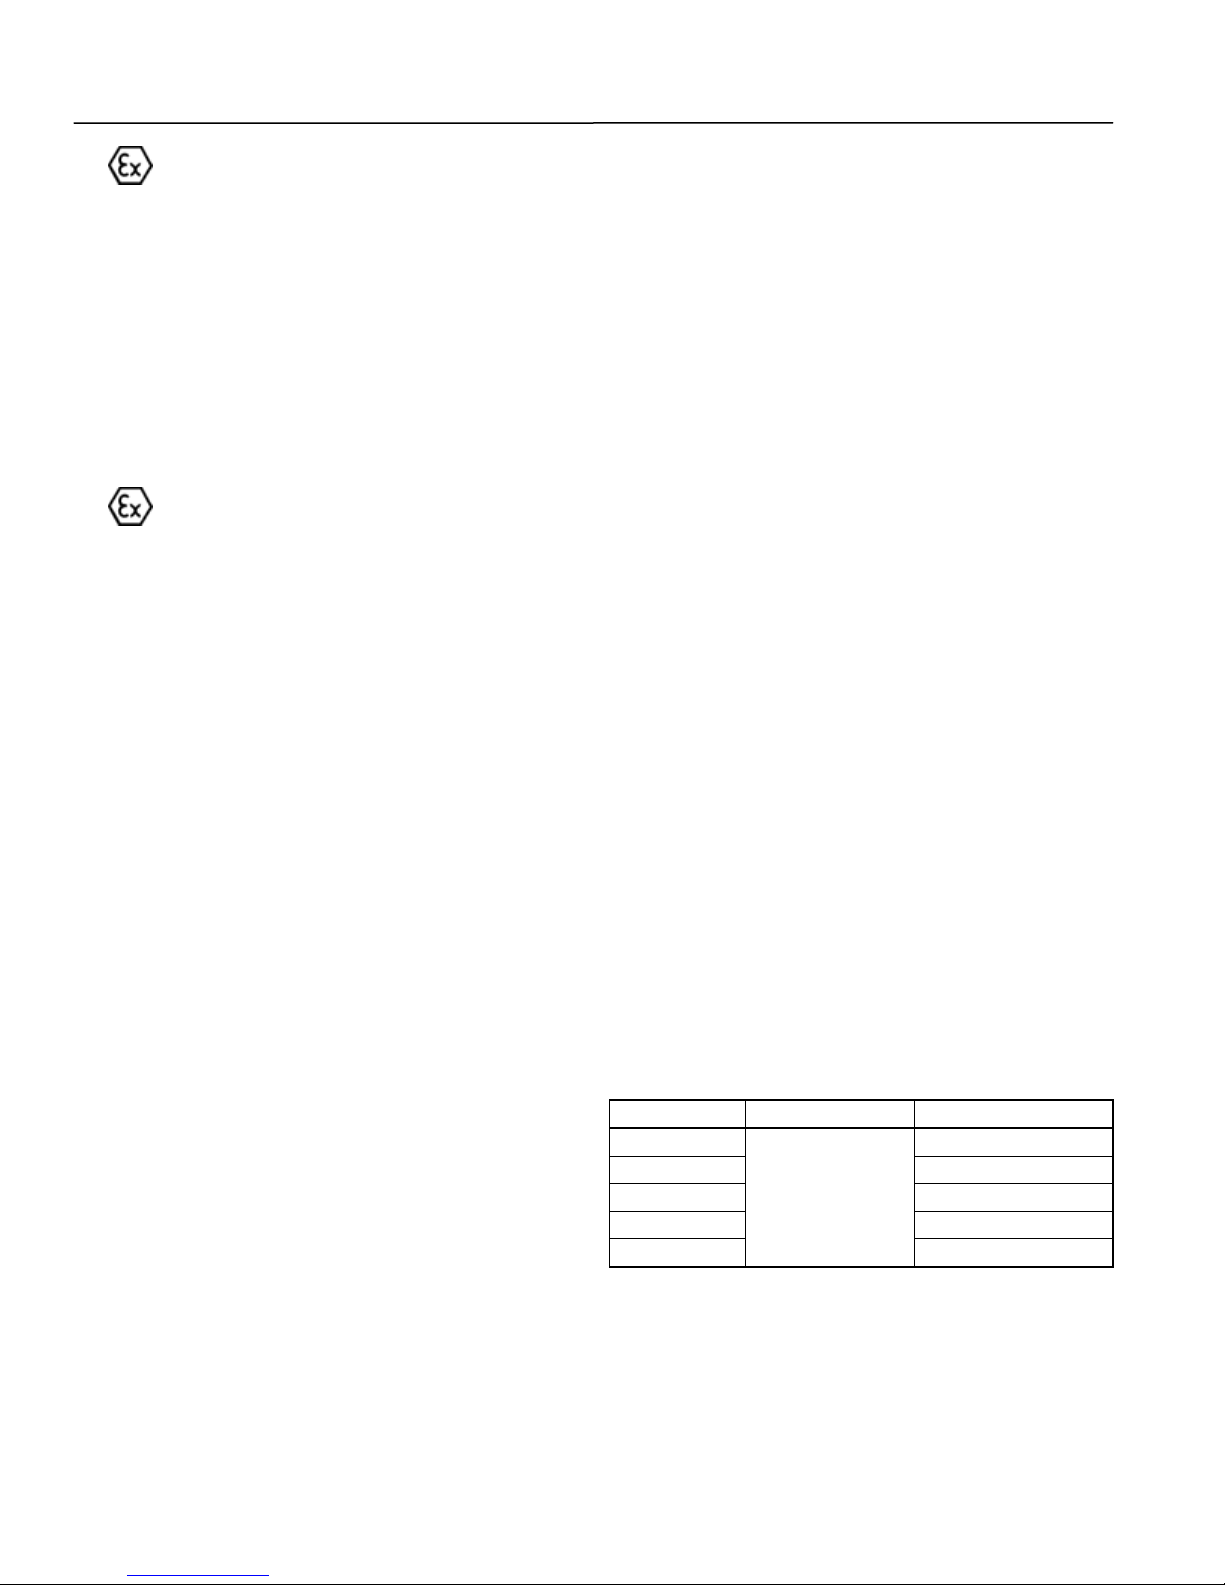
Table 2. Maximum Allowable Pressures
6
Page 13
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
III. EQUIPMENT DESCRIPTION.
RS high-pressure pumps are multi-stage, centrifugal
pumps with radially split casings. The pump consists of
a suction case, a discharge case, plus a number of
interstage casings, all secured with tie bolts. Suction
casing, interstage casings and diffusers are provided
with wear rings. Diffusers are provided with bushings.
Due to prolonged operation, wear rings and bushings
may become worn and/or damaged. Replace all worn
and/or damaged parts with new.
RS high-pressure pumps incorporate special design
refinements, which help to absorb the appreciable axial
thrust generated by their high head operation. Residual
axial thrust is absorbed by the thrust bearings.
CAUTION
Be careful not to mix RS6 and RS9 parts
since RS6 parts are not rated for the pressure
of the RS9.
ATEX and CE require bearing isolators
and metal splash guards to meet requirements.
Other customers may use oil seals and plastic
splash guards.
The bare pump consists of following major parts and
options. Refer to Figures 11 and 12, for the location of
parts identified by item numbers.
Item 1 – Discharge Case. The Discharge Case (1)
houses the impeller (2A or 2X) and diffuser (5A or 5X).
The discharge case is fastened to the suction case with
tie bolts (173) and tie bolt nuts (616) with tie bolt
washers (645).
Item 2A – Impeller, 1st Stage. RS pumps are
equipped with enclosed impellers. The impeller (2A) is
keyed to the shaft (6) by the impeller key (32A) and
located by sleeves and shims. If the RS pump is only a
one stage pump then only the 1st stage impeller is used.
All impellers face the same direction on the shaft.
Item 2X – Impeller. RS pumps are equipped with
enclosed impellers. The impeller (2X) is keyed to the
shaft (6) by the impeller key (32A) and located by
interstage sleeves (58) and shims. All impellers face the
same direction on the shaft.
Item 5A – Diffuser. Diffusers (5A) are inserted in
individual interstage casings. Diffusers are provided with
diffuser bushings (63) and hold wear rings (7X).
Item 5X – Last Stage Diffuser. The last stage diffuser
is located in the discharge case (1). Holds wear ring
(7X) and sits on sleeve bearing (63X).
Item 6 – Shaft. The pump shaft is protected against
wear by interstage sleeves, spacer sleeves, and shaft
sleeves. The shaft (6) of the RS pump is designed for
maximum deflection of 0.002 inch at the face of the
mechanical seal (90). The shaft is also designed to
provide stabilization to the rotor system when pump
operates away from the best efficiency point. A coupling
connects the shaft to the driver shaft. The pump
coupling key (46) holds the coupling in place, causing it
to rotate with the shaft.
Item 16 and 18 – Ball Bearings. A deep-groove
Conrad-type, C3 internal fit radial ball bearing and a
back-to-back mounted ball bearing are housed in the
bearing frame (99) depending on design. The ball
bearings will be designated as 7000 series. Ball
bearings designated in the 7000 series will be duplex
40° angular contact ball bearings. The ball bearing is
held in place by the bearing jam nuts (22). The bearings
are oil lubricated by oil bath.
Item 99 – Bearing Frame. The principal function of the
bearing frame (99) is to carry the loads from the liquid
end of the pump to the base and to transport power from
the power unit to the impeller (2A or 2X). The bearing
frame has a pair of back-to-back mounted angular
contact thrust ball bearings (16). This bearing frame is
designed to be oil lubricated. The bearing frame is
attached to the suction case (9) and discharge case (1)
by tie bolts.
The use of a sight glass constant level oiler (143)
maintains the oil level high enough on the higher of the
two ball bearings so that the ball bearings themselves
provide the motivation for the oil to be moved through
the races of the ball bearings. In addition to the oil lube,
the bearing frame contains the bearing isolator (169).
Item 23 – Base. A grout-able base (23) is designed to
provide adequate support for the pump and motor so
pump can be operated without base deflection,
excessive vibration, or resonance. The pump is attached
to the base with stud (634) and hex nut (614). Grouting
of this type of base is required by Carver Pump
Company.
Item 90 and 91 – Mechanical Seal. Mechanical seals
(90 and 91) are to be used. Complete mechanical seal
instructions should be obtained from the seal
manufacturer. The standard seal chamber dimensions
are shown in Figure 1.
Item 111 – Interstage Case. The interstage case
houses the impeller (2A or 2X) and diffuser (5A). The
interstage casings are all secured with tie bolts to the
7
Page 14
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
suction (9) and discharge (1) casings. Interstage
casings are provided with wear rings (7X). O-rings (89D)
seal the individual interstage casings. A one stage pump
does not have an interstage case.
IV. EFFECTS OF FLUIDS.
Solids in the fluid pumped may cause
internal damage to pump casing and damage
to the seal faces with resulting Hazardous
conditions. Care is to be taken to ensure that
the process fluid is clear of solids and debris.
A. NET POSITIVE SUCTION HEAD (NPSH). Any
liquid, hot or cold, must be pushed into the impeller of
the pump by some absolute pressure, such as the
atmosphere or the vessel pressure from which the pump
takes its action.
The head in feet of liquid necessary to maintain the
required flow into the pump is called the Net Positive
Suction Head (NPSH). This value is measured above
the vapor pressure of the liquid at the pumping
temperature.
NPSH is commonly expressed in two ways: the NPSH
required by the pump, and shown on the pump curve, is
the head needed to cover the losses in the pump
suction and the energy required to enable the liquid to
climb onboard the leading edge of the impeller vane.
The NPSH available is that inherent in the system,
taking into account friction losses in suction piping,
valves, fittings, etc. In all cases, the NPSH available,
measured above vapor pressure, must exceed the
NPSH required in order to push the liquid into the pump.
B. CHANGING PUMP SPEED. Changing the speed of
a centrifugal pump affects the capacity, total head,
NPSH required and the brake horsepower. In general
the capacity will vary in a direct ratio with the speed,
whereas the total head and NPSH required will vary as
the ratio of the speed squared. The brake horsepower
will vary as the ratio of the speed cubed.
C. EFFECTS OF VISCOSITY. The pump is designed
to deliver rated capacity at rated head for a liquid with a
particular viscosity. When pump is handling heavy
viscous liquid, the viscosity of the liquid must allow it to
be pumped easily. The liquid may have to be heated
prior to starting the pump. When contemplating
operation at some viscosity other than that for which the
pump was originally designed, check with Carver Pump
Company.
D. EFFECTS OF SPECIFIC GRAVITY. The capacity
and total head in feet of liquid developed by a centrifugal
pump are fixed for every point on the curve and are
always the same for the same speed. Neither capacity
nor total head will be affected by a change in the
specific gravity of the liquid pumped. However, since the
discharge pressure in Pounds per Square Inch (PSI)
and the brake horsepower required driving the pump are
functions of the specific gravity of the liquid, both will be
affected in direct proportion by any change in specific
gravity. Therefore, an increase in specific gravity will
raise the discharge pressure and is dangerous as it
might overload the pump's driver, or exceed the pump
casing allowable pressure.
V. TECHNICAL DATA.
Specifications and operating limits should be recorded
on a Service Record Page; an example is located in the
front matter of this manual. Record the necessary
information upon receipt of the pumping unit.
Noise Levels. Noise levels may exceed 85dBa at 1
meter during operation. Ear protection must be worn
whenever working in high noise locations.
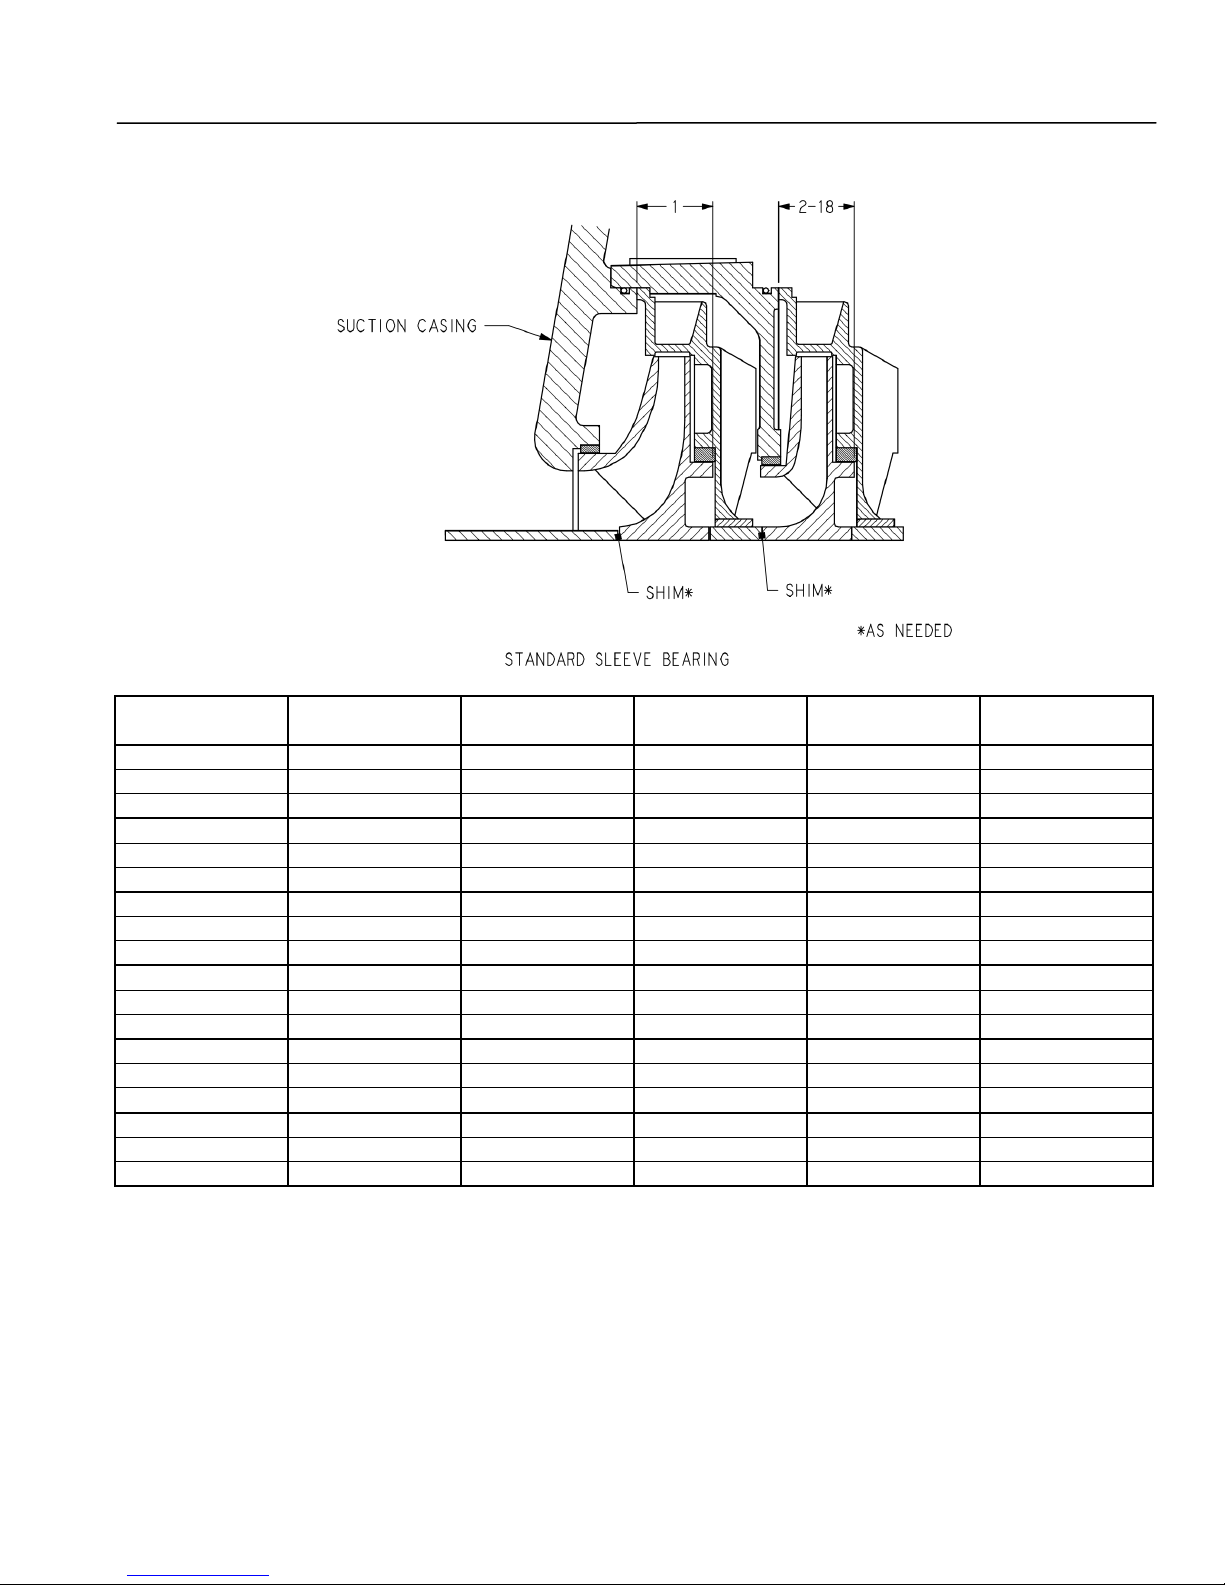
Axial Impeller Alignment Control Dimensions. Axial
impeller alignment control dimension are located in
Table 3 and are arranged by pump size.
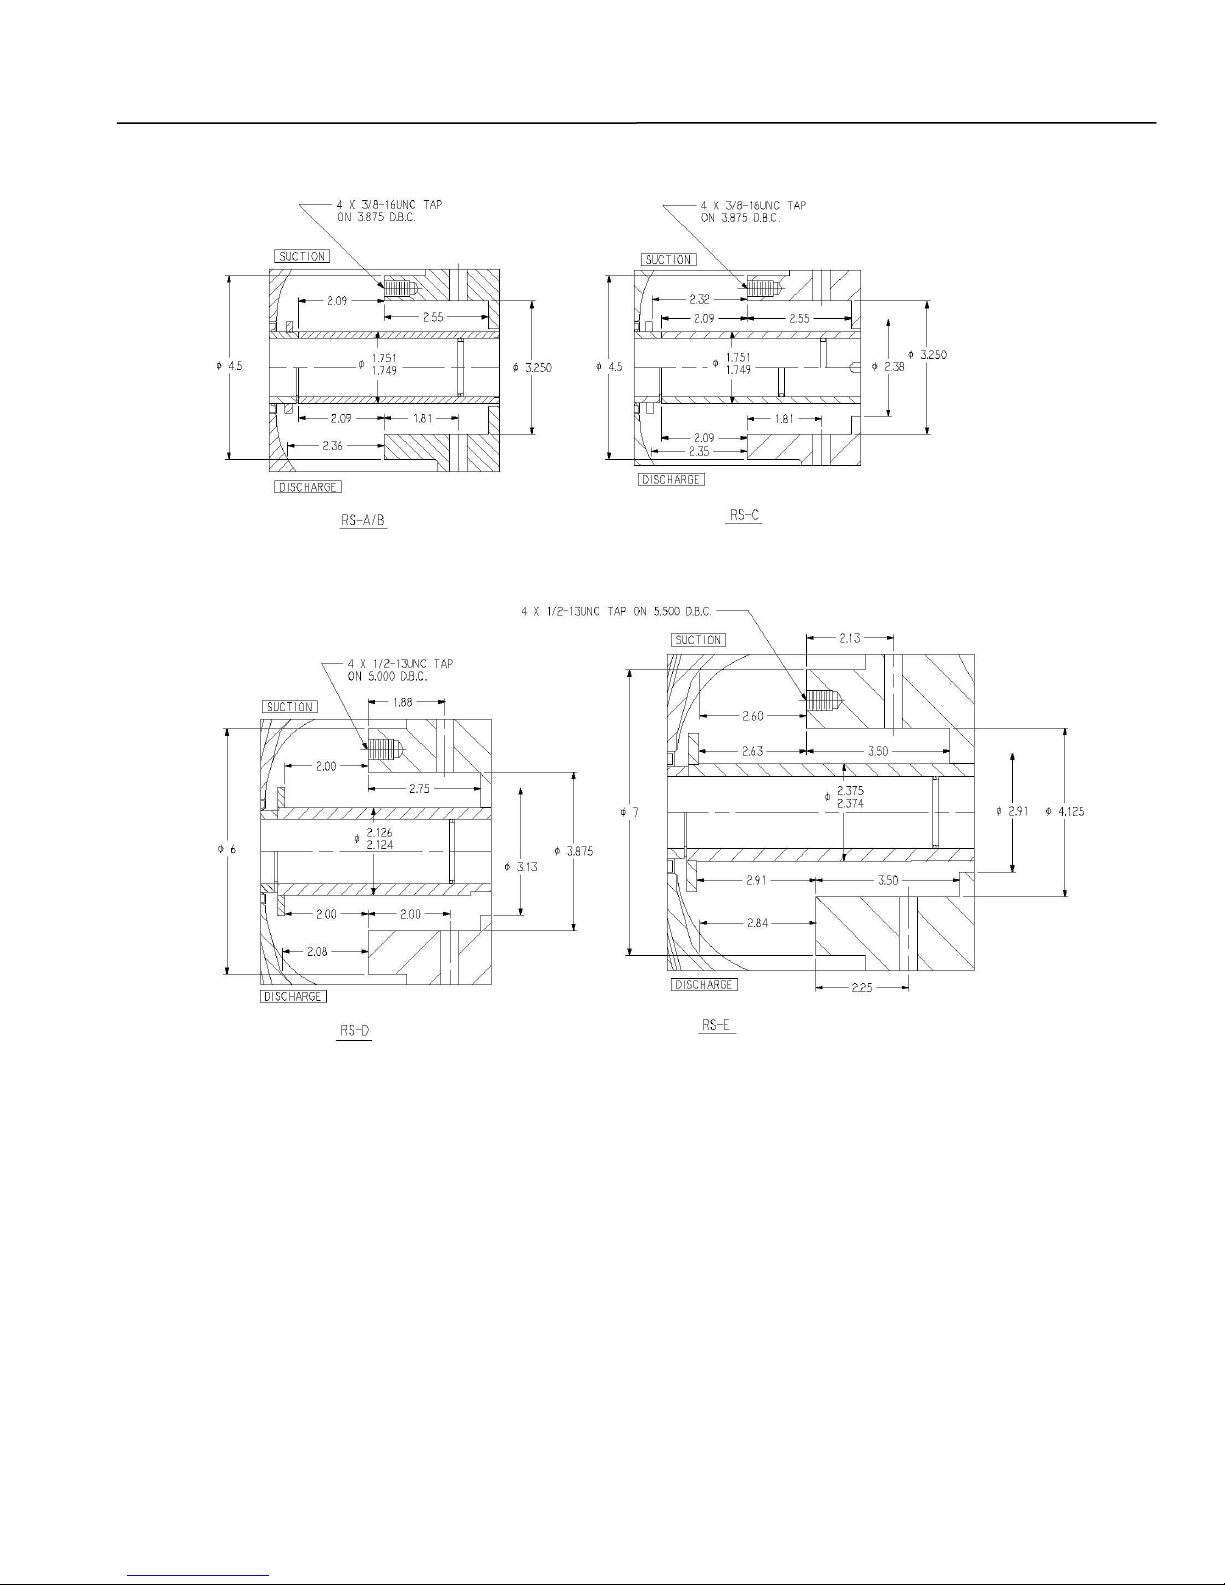
Seal Chamber Dimensions. Standard seal chamber
dimensions are located in Figure 1 and are arranged by
pump size.
Basic Design Features. Basic design features of the
pump are located in Tables 3, 4, 5, 6, 7, 10, and Figures
2 and 3 and are arranged by pump model.
Key Mechanical Data. Key mechanical data for the
pump is located in Table 8 and is arranged by pump
model.
Permissible Nozzle Loads. The forces and moments
in Table 9 are to be understood as the limit for a single
acting force or moment along the particular coordinate
axes or any resultant of two or more forces and
moment.
8
Page 15
RS – Multi-Stage, I-280
Stages
Pump Size A
(Inches)
Pump Size B
(Inches)
Pump Size C
(Inches)
Pump Size D
(Inches)
Pump Size E
(Inches)
1
1.147
1.150
1.267
1.580
2.093
2
1.144
1.143
1.263
1.635
1.998
3
1.141
1.140
1.260
1.632
1.995
4
1.138
1.137
1.257
1.629
1.992
5
1.135
1.134
1.254
1.626
1.989
6
1.132
1.131
1.251
1.623
1.986
7
1.129
1.128
1.248
1.620
1.983
8
1.126
1.125
1.245
1.617
1.980
9
1.123
1.122
1.242
1.614
N/A
10
1.12
1.119
1.239
1.611
N/A
11
1.117
1.116
1.236
1.608
N/A
12
1.114
1.113
1.233
1.605
N/A
13
1.111
1.110
N/A
N/A
N/A
14
1.108
1.107
N/A
N/A
N/A
15
1.105
1.104
N/A
N/A
N/A
16
1.102
1.101
N/A
N/A
N/A
17
1.099
1.098
N/A
N/A
N/A
18
1.096
1.095
N/A
N/A
N/A
Centrifugal Pump 280 – 16.03.EN
Table 3. Axial Impeller Alignment Control Dimensions
*Additional stages will require compensation for interstage compression, on average .003 inch per stage. Use .010
inch shim as needed. Refer to Section XI, Paragraphs E.
9
Page 16
RS – Multi-Stage, I-280
Stages
Pump Size A
(Inches)
Pump Size B
(Inches)
Pump Size C
(Inches)
Pump Size D
(Inches)
Pump Size E
(Inches)
1
-.110
-.110
-.125
.137
.185
2
-.113
-.113
-.128
.134
.182
3
-.116
-.116
-.131
.131
.179
4
-.119
-.119
-.134
.128
.176
5
-.122
-.122
-.137
.125
.173
6
-.125
-.125
-.140
.122
.170
7
-.128
-.128
-.143
.119
.167
8
-.131
-.131
-.146
.116
.164
9
-.134
-.134
-.149
.113
N/A
10
-.137
-.137
-.152
.110
N/A
11
-.140
-.140
-.155
.107
N/A
12
-.143
-.143
-.158
.104
N/A
13
-.146
-.146
N/A
N/A
N/A
14
-.149
-.149
N/A
N/A
N/A
15
-.152
-.152
N/A
N/A
N/A
16
-.155
-.155
N/A
N/A
N/A
17
-.158
-.158
N/A
N/A
N/A
18
-.161
-.161
N/A
N/A
N/A
Low NPSH
Impeller
See note below
See note below
See note below
See note below
See note below
2 - 18
1 (Discharge Side)
Low NPSH Impeller
(Suction)
Centrifugal Pump 280 – 16.03.EN
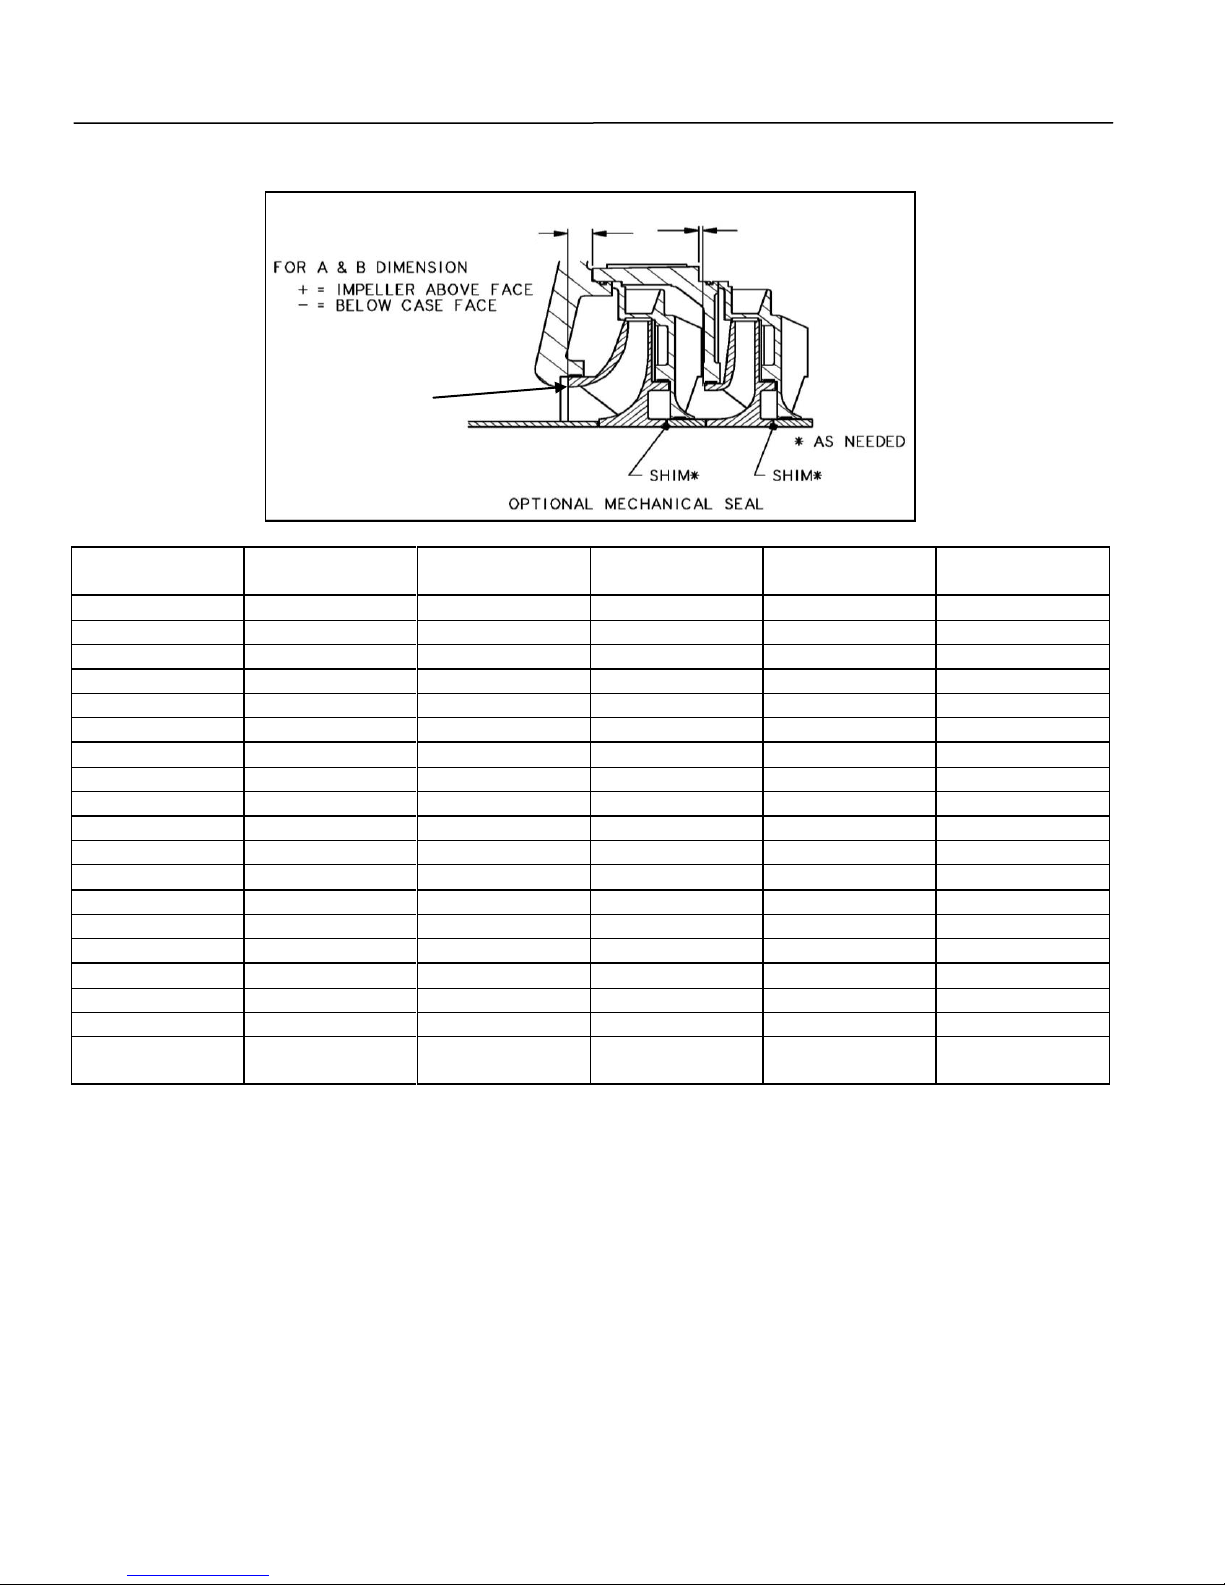
Table 3. Axial Impeller Alignment Control Dimensions - Continued
*Additional stages will require compensation for interstage compression, on average .003 inch per stage. Use .010
inch shim as needed. Refer to Section XI, Paragraphs F.
RSA No NPSH Impeller
RSB .210 – [#of stages X (.003) - Gaps] = NPSH Impeller Setting
RSC .538 – [#of stages X (.003) - Gaps] = NPSH Impeller Setting
RSD .792 – [#of stages X (.003) - Gaps]= NPSH Impeller Setting
RSE .210 – [#of stages X (.003) - Gaps] = NPSH Impeller Setting
10
Page 17
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
Figure 1. Seal Chamber Dimensions
11
Page 18
RS – Multi-Stage, I-280
Pump Model
At Impeller (Inches)
At Coupling (Inches)
A
1.437
1.250
B
1.437
1.250
C
1.437
1.250
D
1.574
1.500
E
1.771
1.625
Pump Model
Sleeve Bearing New
(Inches)
Sleeve Bearing
Replacement Limits
(Inches)
Sleeve
(Ø = Diameter Measured)
New (Inches)
Replace (Inches)
A
1.758/1.760
Ø > 1.762
1.751/1.749
Ø < 1.746
B
1.758/1.760
Ø > 1.762
1.751/1.749
Ø < 1.746
C
1.758/1.760
Ø > 1.762
1.751/1.749
Ø < 1.746
D
1.972/1.974
Ø >1.976
1.965/1.963
Ø < 1.961
E
2.382/2.384
Ø >2.386
2.375/2.373
Ø < 2.371
Pump Model
Suction End (Inches)
(from end of sleeve to face of collar)
A
3.100
B
3.100
C
3.100
D
4.322
E
4.500
Centrifugal Pump 280 – 16.03.EN
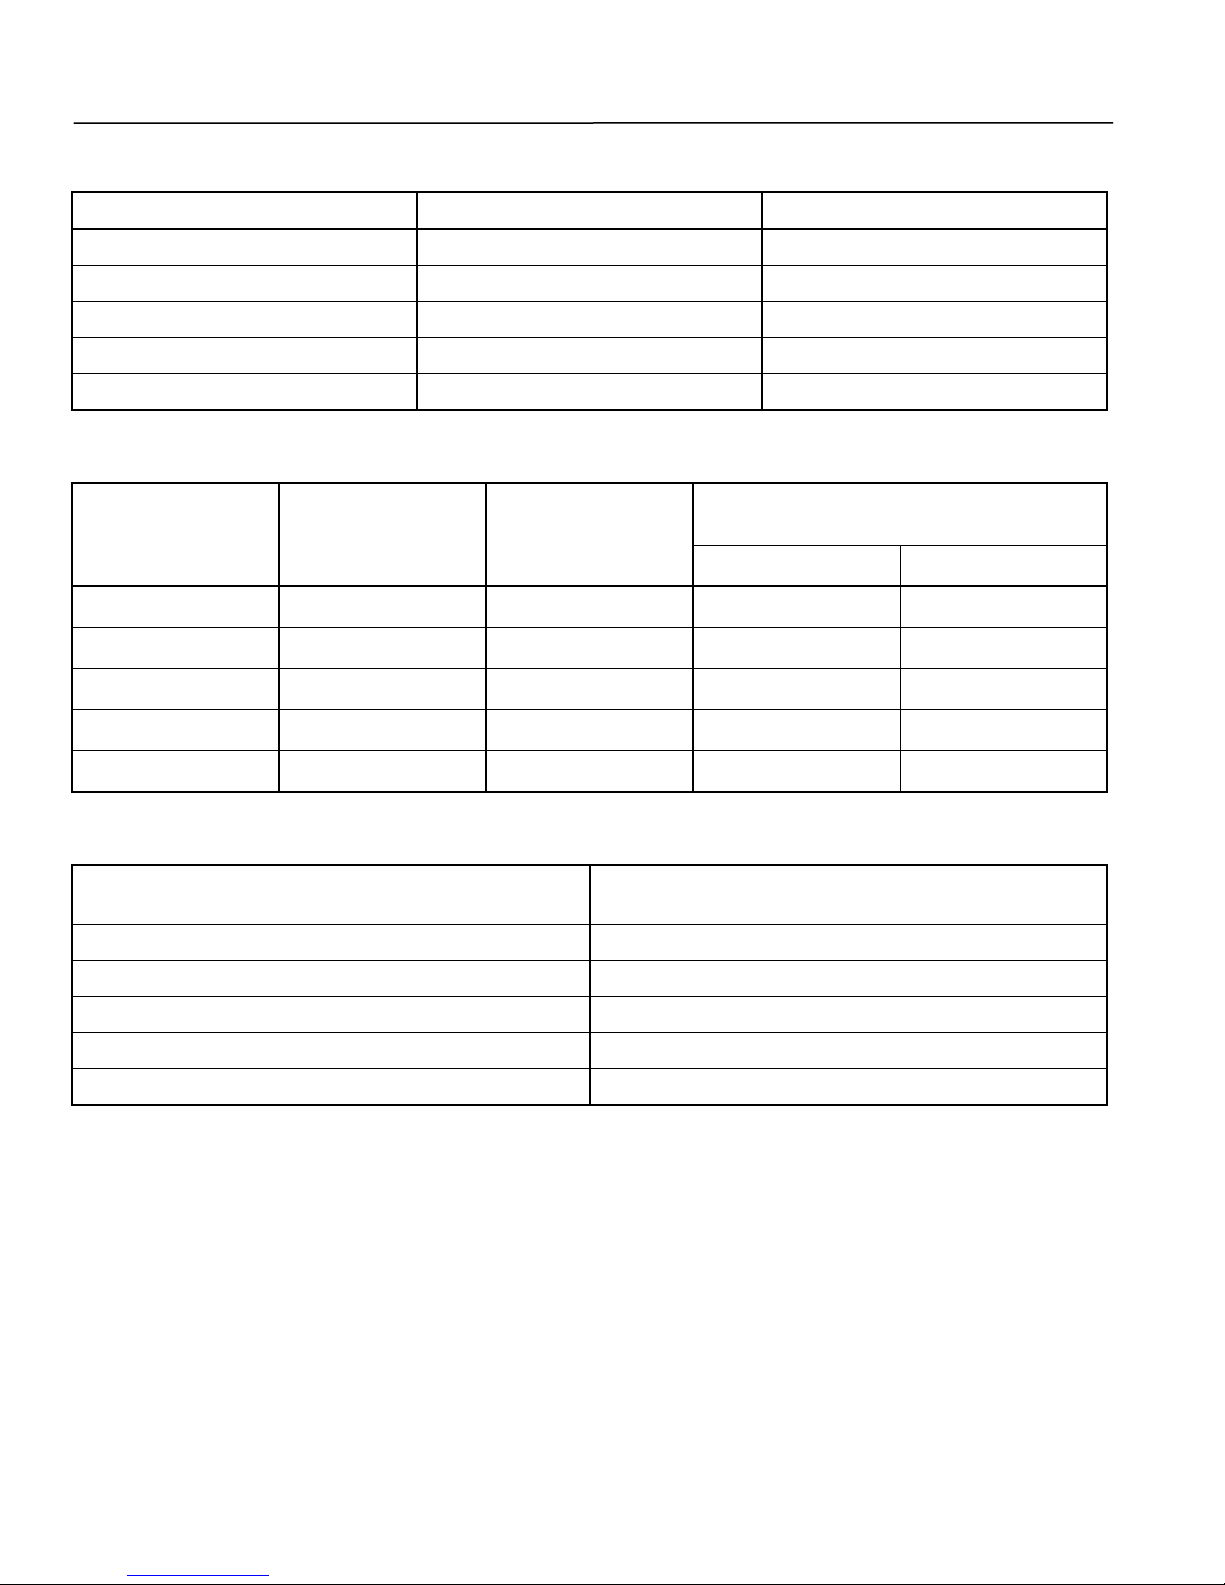
Table 4. Shaft Dimensions
Table 5. Sleeve Bearing Dimensions
Table 6. Standard Design Pump Mechanical Seal Settings
12
Page 19
RS – Multi-Stage, I-280
Pump
Model
Discharge End (Seal Type 1)
(for reference only) – Inches
(from face of box to face of
collar)
Discharge End (Seal Type
8B1) (for reference only) –
Inches
(from face of box to face of
collar)
Suction end (Seal Type 1 or
21)
- Inches
(from face of box to face of
collar)
A
.750
1.375
1.000
B
.750
1.375
1.000
C
.750
1.375
1.000
D
2.062
1.750
1.312
E
1.792
1.812
1.594
Item
Pump Model
A, B C D
E
Maximum Speed
3500 RPM
Max HP – (17-4 PH shaft)
370
370
603
900
Max HP – (416 SS Shaft)
308
308
500
690
WR2 of Rotor – 1st Stage (lb-In2)
14.6
30.8
36.7
106.5
WR2 of Rotor –
each Stage (lb-In2)
10.2
26.7
31.1
94.4
Lubrication Method (Standard)
Oil – ISO Grade 68
L10 Bearing Life (hrs) - Thrust
50,000
L10 Bearing Life (hrs) - Radial
50,000
Radial Bearing Type
307
307
308
309
Thrust Bearing Type
7307
7307
7308
7309
Plan 13
Plan 11
Plan 13
Plan 23
Plan 21
Centrifugal Pump 280 – 16.03.EN
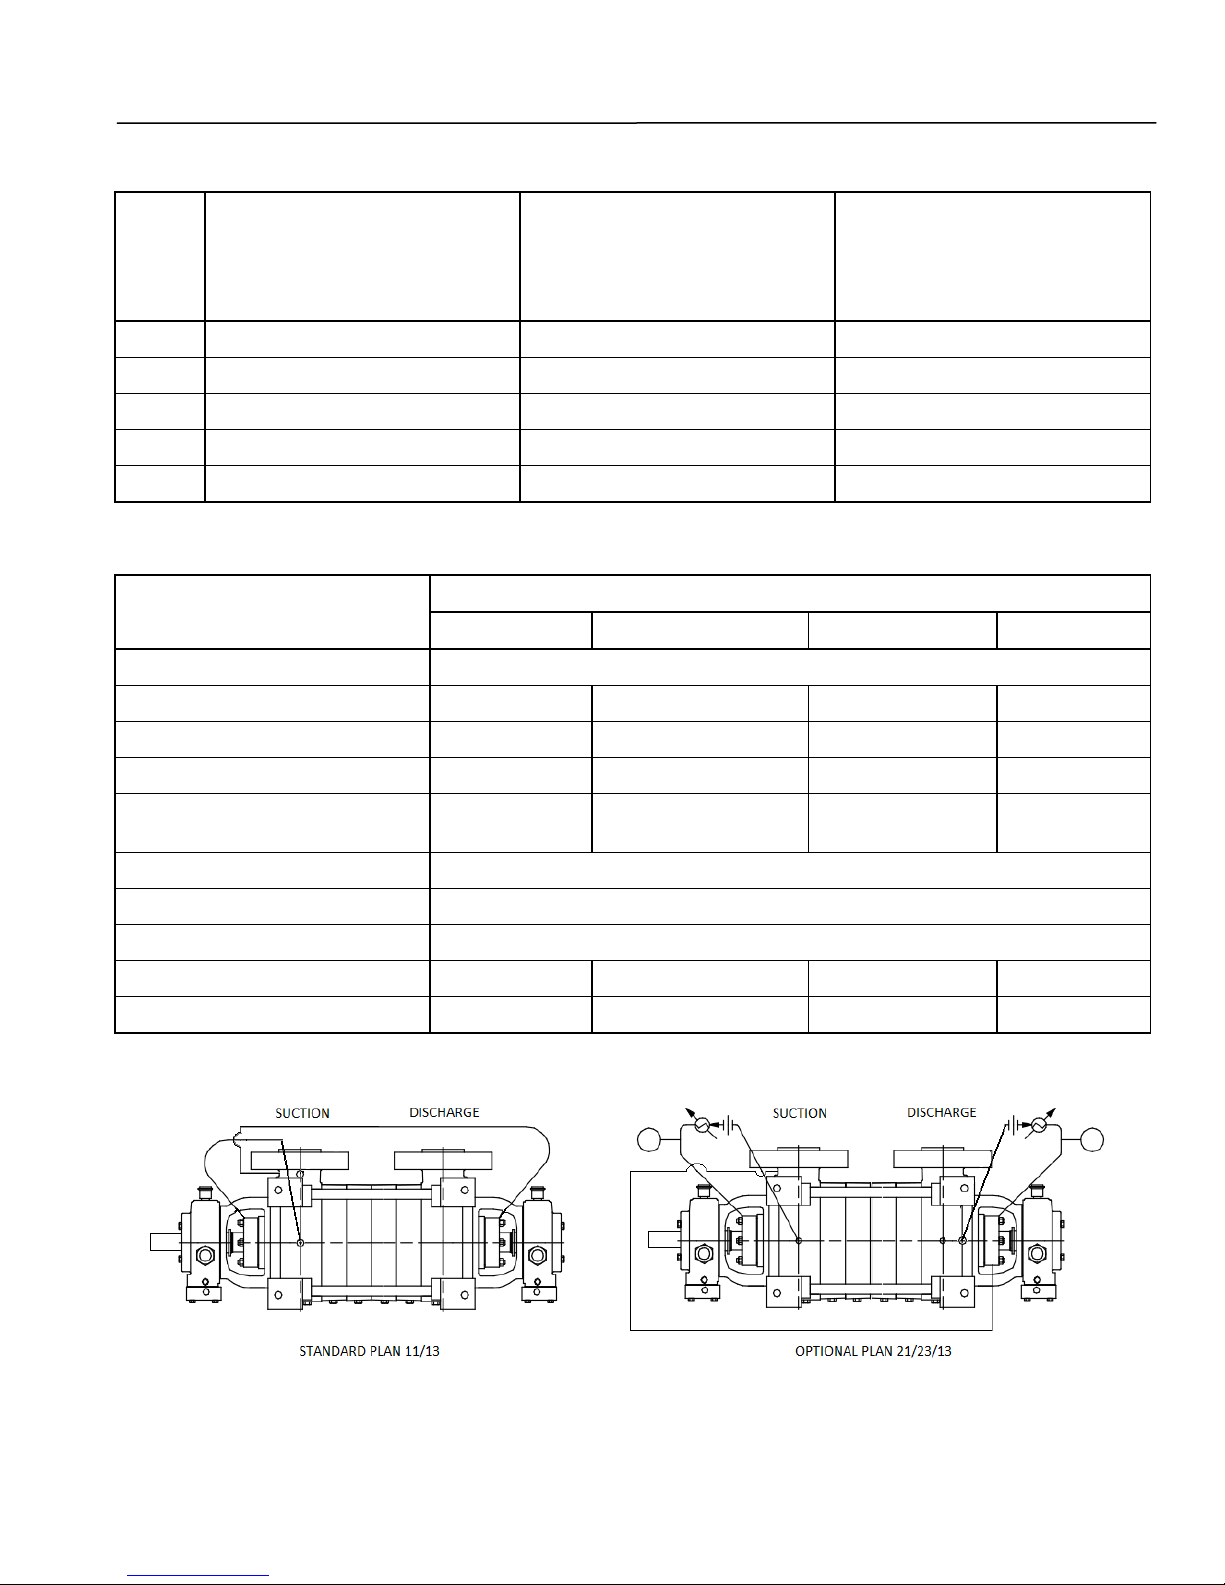
Table 7. Optional Design Pump Mechanical Seal Settings
Table 8. Key Mechanical Data
The standard seal flush plans provided with the optional outboard mechanical seal are shown below.
Recirculation from Suction Point to Seal Recirculation from Discharge Point thru a TI
and Heat Exchanger to Seal
Figure 2. Standard Seal Flush Plans
13
Page 20
RS – Multi-Stage, I-280
OPTIONAL DESIGN
END VIEW
SIDE VIEW
IN/OUT
¼ NPT
IN/OUT
¼ NPT
OIL
STANDARD DESIGN
Centrifugal Pump 280 – 16.03.EN
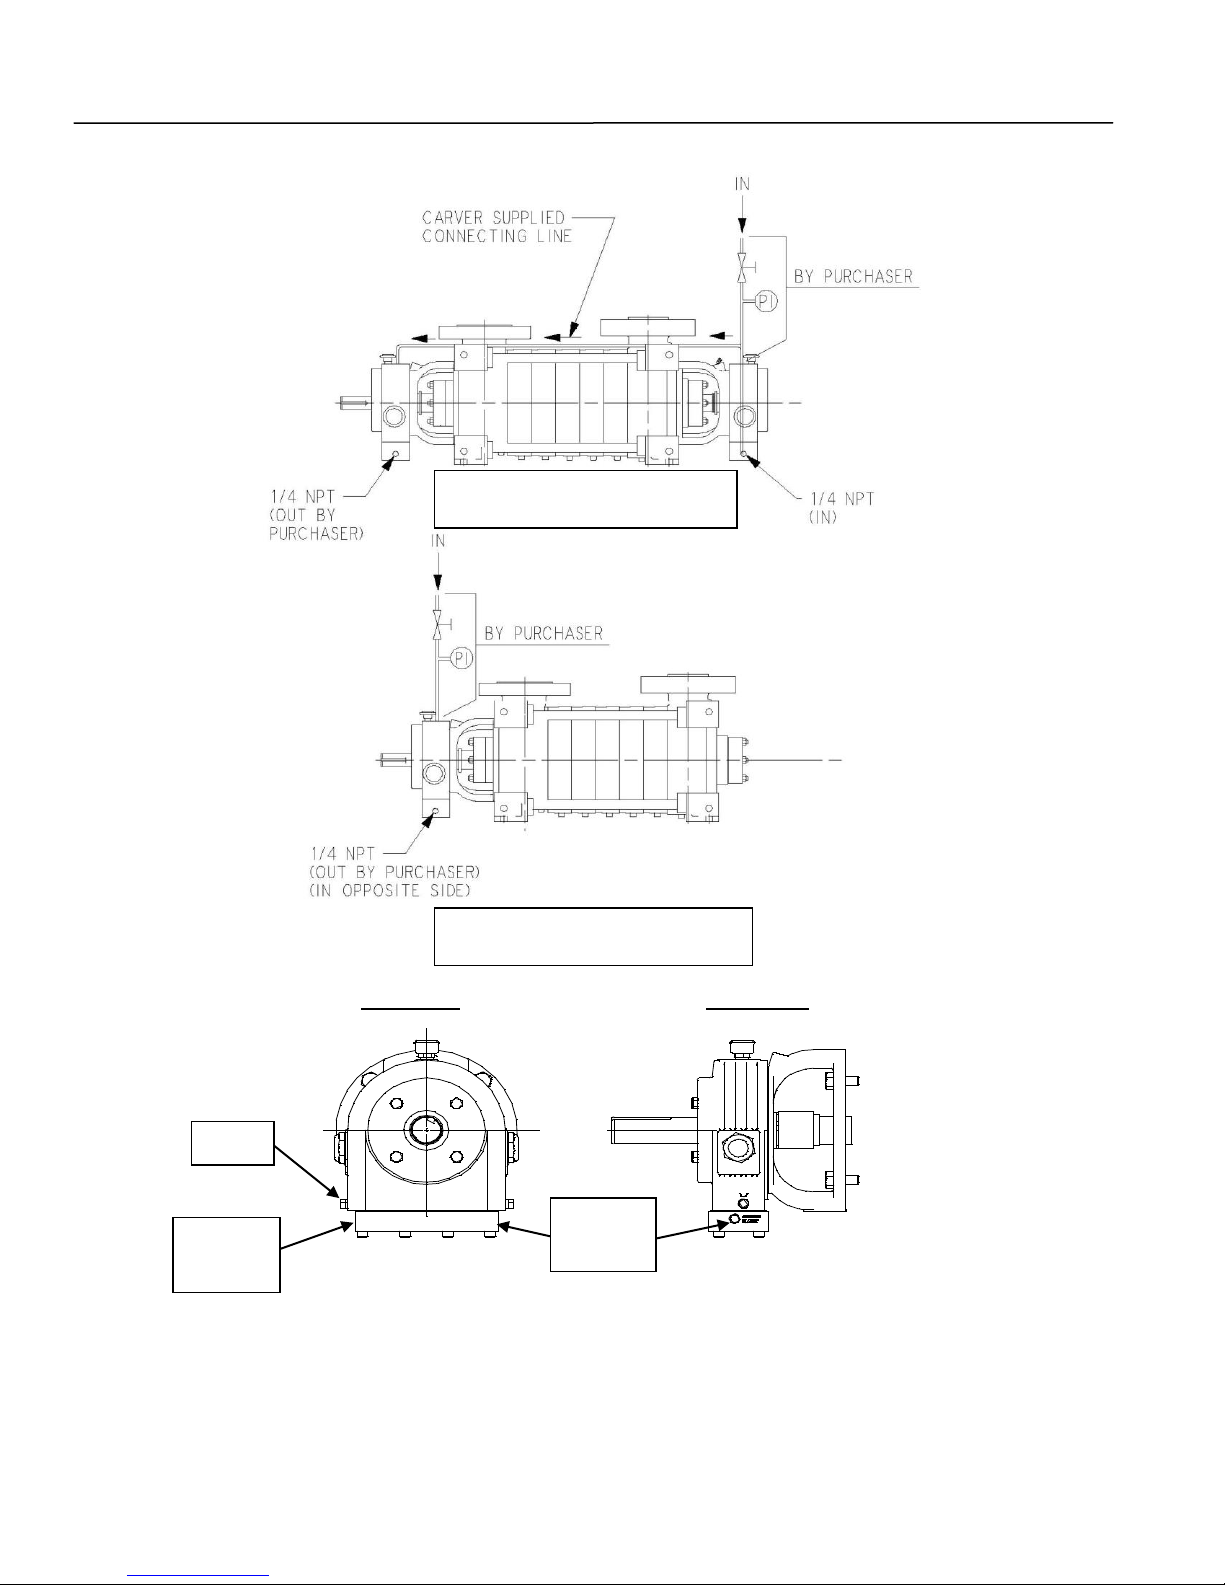
14
Figure 3. Bearing Frame Water Cooling
Page 21
RS – Multi-Stage, I-280
Size
Side Connection
Top Connection
FX
FY
FZ
MX
MY
MZ
FX
FY
FZ
MX
MY
MZ
A, B
256
555
567
643
839
370
710
232
732
552
839
266 C 266
573
595
746
988
414
710
244
778
649
988
311 D 399
822
827
1,290
1,599
801
1,130
352
997
1,083
1,599
565 E 599
1,228
1,281
2,361
3,003
1,411
1,673
530
1,575
2,007
3,003
1,011
Pump Model
Speed (RPM)
Minimum Flow (GPM)
Minimum Continuous
Flow (GPM)
A
1450
15
20
1750
20
25
2900
25
40
3500
35
50 B 1450
15
40
1750
20
50
2900
25
80
3500
35
100 C 1450
30
75
1750
40
90
2900
50
150
3500
100
180
D
1450
30
125
1750
50
150
2900
120
250
3500
200
300 E 1450
30
200
1750
50
250
2900
150
400
3500
200
500
Centrifugal Pump 280 – 16.03.EN
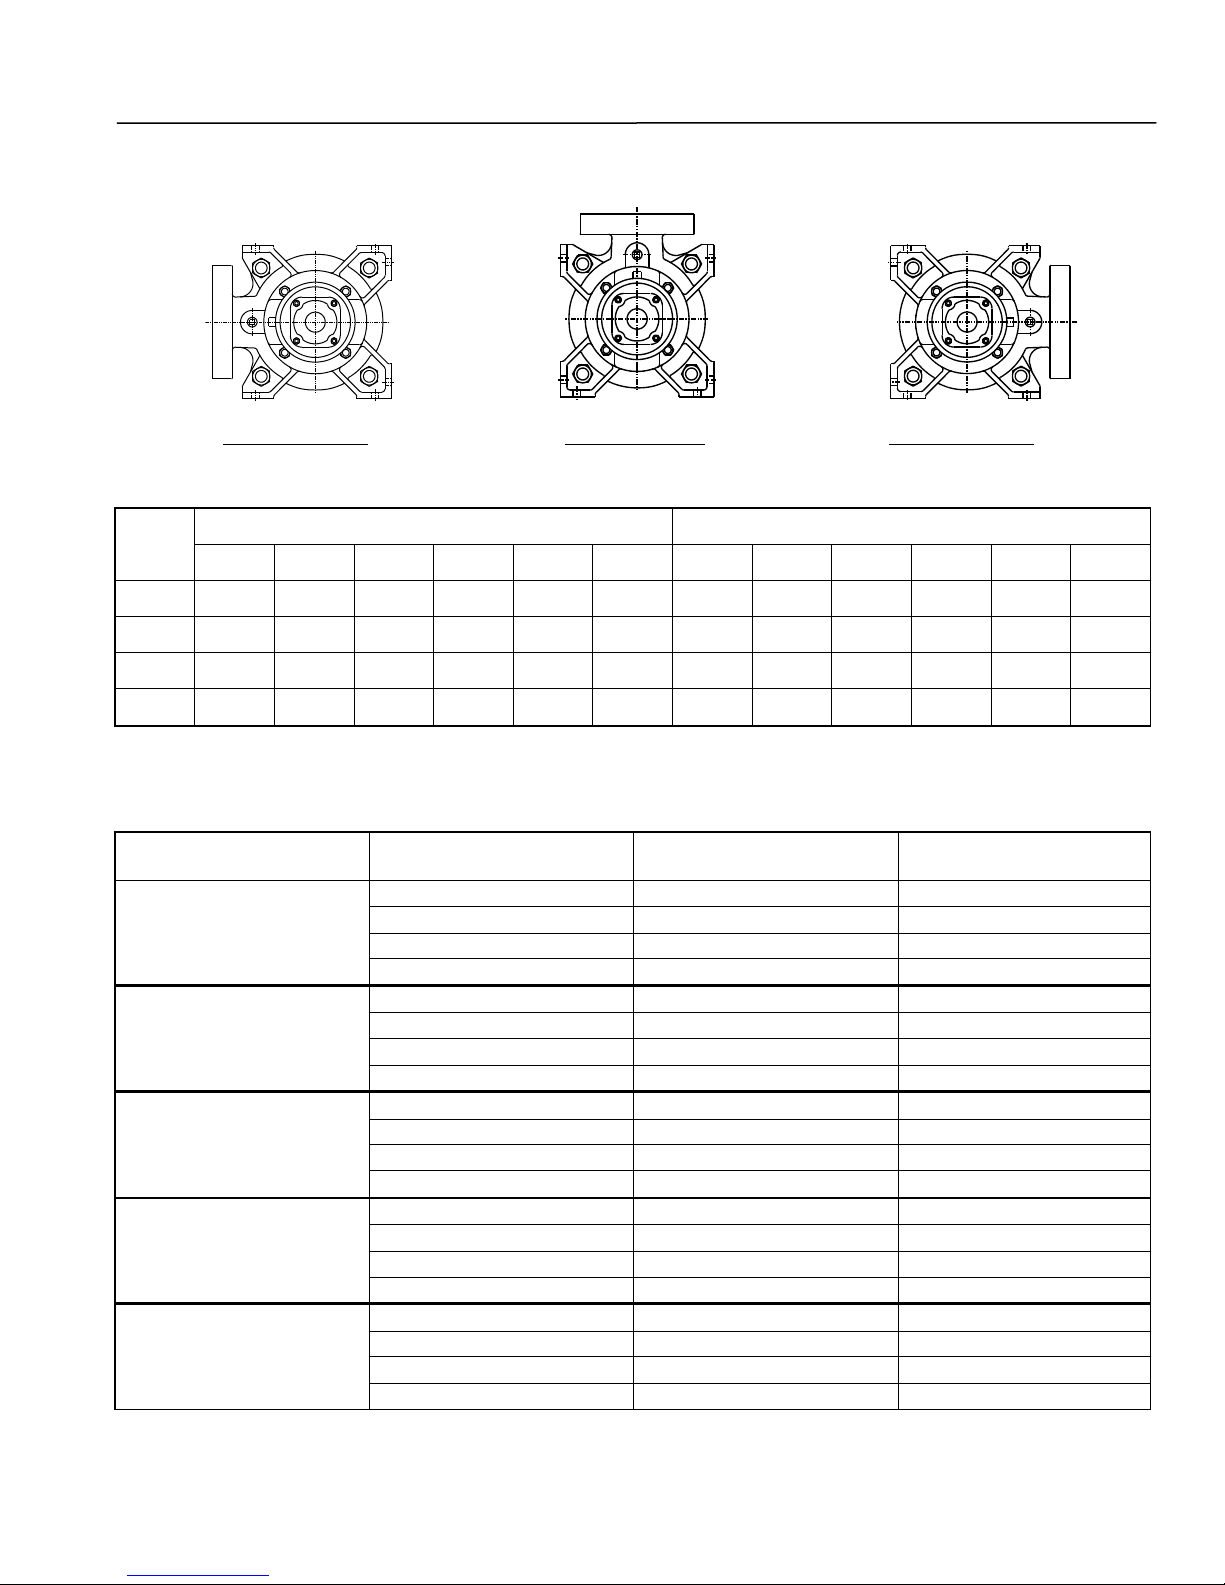
Table 9. Permissible Nozzle Loads
X X X
Y Y Y
Side Connection Top Connection Side Connection
Suction Position A Suction Position B Suction Position C
Discharge Position 1 Discharge Position 2 Discharge Position 3
M = Moments measured in Foot-Pounds (FT-lbs)
F = Forces measured in Pounds (lbs)
Table 10. Minimum Flow Rates RS-6 and RS-9
15
Page 22
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
VI. INSPECTION AND STORAGE.
CAUTION
A. INSPECTION. Upon receipt of the shipment,
unpack and inspect the pumping unit and individual
parts to insure none are missing or damaged. Carefully
inspect all boxes and packing material for loose parts
before discarding them. Check to make sure the
shipment complies with the purchase order. Immediately
report any missing parts or damage incurred during
shipment to the factory and to the Transportation
Company and file your “damage and/or lost in shipment”
claim with the carrier.
B. PACKING FOR RETURN. If the pumping unit is
sent back to Carver Pump Company for repair, drain the
unit, and re-seal all flanges and connections that were
covered or plugged. Ship the pump(s) in an assembled
condition to prevent damage to sealing faces of
individual components. A Return Goods Authorization
(RGA) and a Material Safety Data Sheet (MSDS) is
required on all returned pumps. Copies of MSDS
records should be kept and maintained by the customer.
The customer is responsible for cleaning and flushing
the pump before it is returned to the factory. Make sure
to specify the fluid used in the service.
C. STORAGE OF PUMP. If the equipment is not to be
immediately installed and operated, store it in a clean,
dry, well ventilated place, free from vibrations, moisture
and rapid or wide variations in temperature.
NOTE
Storage requirements vary depending on
climatic environment, length of storage and
equipment. For storage periods of three months
or longer, contact manufacturer for specific
instructions. Improper storage could damage
equipment and would result in non-warranty
covered restoration of non-warranty covered
product failures.
When storing the pump up to three months rotate the
shaft for several revolutions at least once per month to
coat the bearings with lubricant, retard oxidation and
corrosion, and prevent possible false brinelling.
The motor bearings should be prepared for storage
according to the motor manufacturer’s instructions, in
the motor manufacturer’s maintenance manual, which
should come with the motor.
For shipment and long term storage purposes
the pump ball bearing shall be fogged once
every 30 days during storage with a rust
retardant compatible with the oil used in the
system to prevent rusting.
A pump which is made of iron or steel that sits
in extreme heat, high humidity, or full or
partially full water over 30 days will rust and will
most likely seize. If the pump rusts and/or
seizes, a complete overhaul and repair may be
necessary to refurbish the pump.
Consider a unit to be in storage when:
1. It has been delivered to the job site and is
waiting to be installed.
2. It has been installed but operation is delayed
pending completion of construction.
3. There are long (30 days or more) periods
between operating cycles.
4. The plant (or department) is shut down for
periods of longer than 30 days.
Measures to be taken for prolonged shutdown of
installed pumping unit. If the pumping unit remains
installed a periodic check of operation is in order to
make sure that the pump is always ready for instant
start-up and to prevent the formation of deposits within
the pump and the pump intake area. Start up the
pumping unit regularly once a month or once every 3
months for a short time (approximately 5 minutes)
during prolonged shutdown periods. Prior to operation
check run ensure that there is sufficient liquid available
for operating the pump.
Interim Storage (Indoors)/Preservation. When the
unit is temporarily put into storage, only the wetted low
alloy must be preserved. Commercially available
preservatives can be used for this purpose. Please
observe the manufacturer’s instructions for
application/removal.
The unit/pump should be stored in a dry room where the
atmospheric humidity is as constant as possible.
If stored outdoors, the unit and crates must be covered
by waterproof material to avoid any contact with
humidity.
16
Protect all stored goods against humidity, dirt, vermin
and unauthorized access!
Page 23
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
All openings of the assembled unit components are
closed and must only be opened when required during
installation.
All blank parts and surfaces of the pump are oiled or
greased (silicone-free oil and grease) to protect them
against corrosion.
VII. INSTALLATION.
A. LOCATION. The pump assembly should be
located in an area that will permit periodic inspection
and maintenance. Head room and access should be
provided and all units should be installed in a dry
location with adequate drainage. The discharge piping
should be direct with as few elbows and fittings as
possible.
The pump assembly should be installed as close to the
fluid as possible. A short, direct suction pipe can be
used to keep suction losses at a minimum. If possible,
locate the pump so fluid will flow by gravity to the
suction opening. The discharge piping should be direct
with as few elbows and fittings as possible. The total Net
Positive Suction Head Available (NPSHA), which
includes the suction lift and pipe friction losses, must be
greater than the Net Positive Suction Head Required
(NPSHR) by the pump.
B. HANDLING.
CAUTION
Use a hoist with adequate lifting capacity.
Do not pick up the complete unit by the motor
or the pump shafts or motor lifting eyes.
If the pumping unit slips out of the sling
arrangement, it may cause injury to personnel
and/or damage to the pumping unit.
Moving the unit requires proper preparation and
handling. Always make sure that the pump or the
pumping unit remains in a horizontal position while
being moved and cannot slip out of the transport
suspension arrangement. Use a sling for pumps without
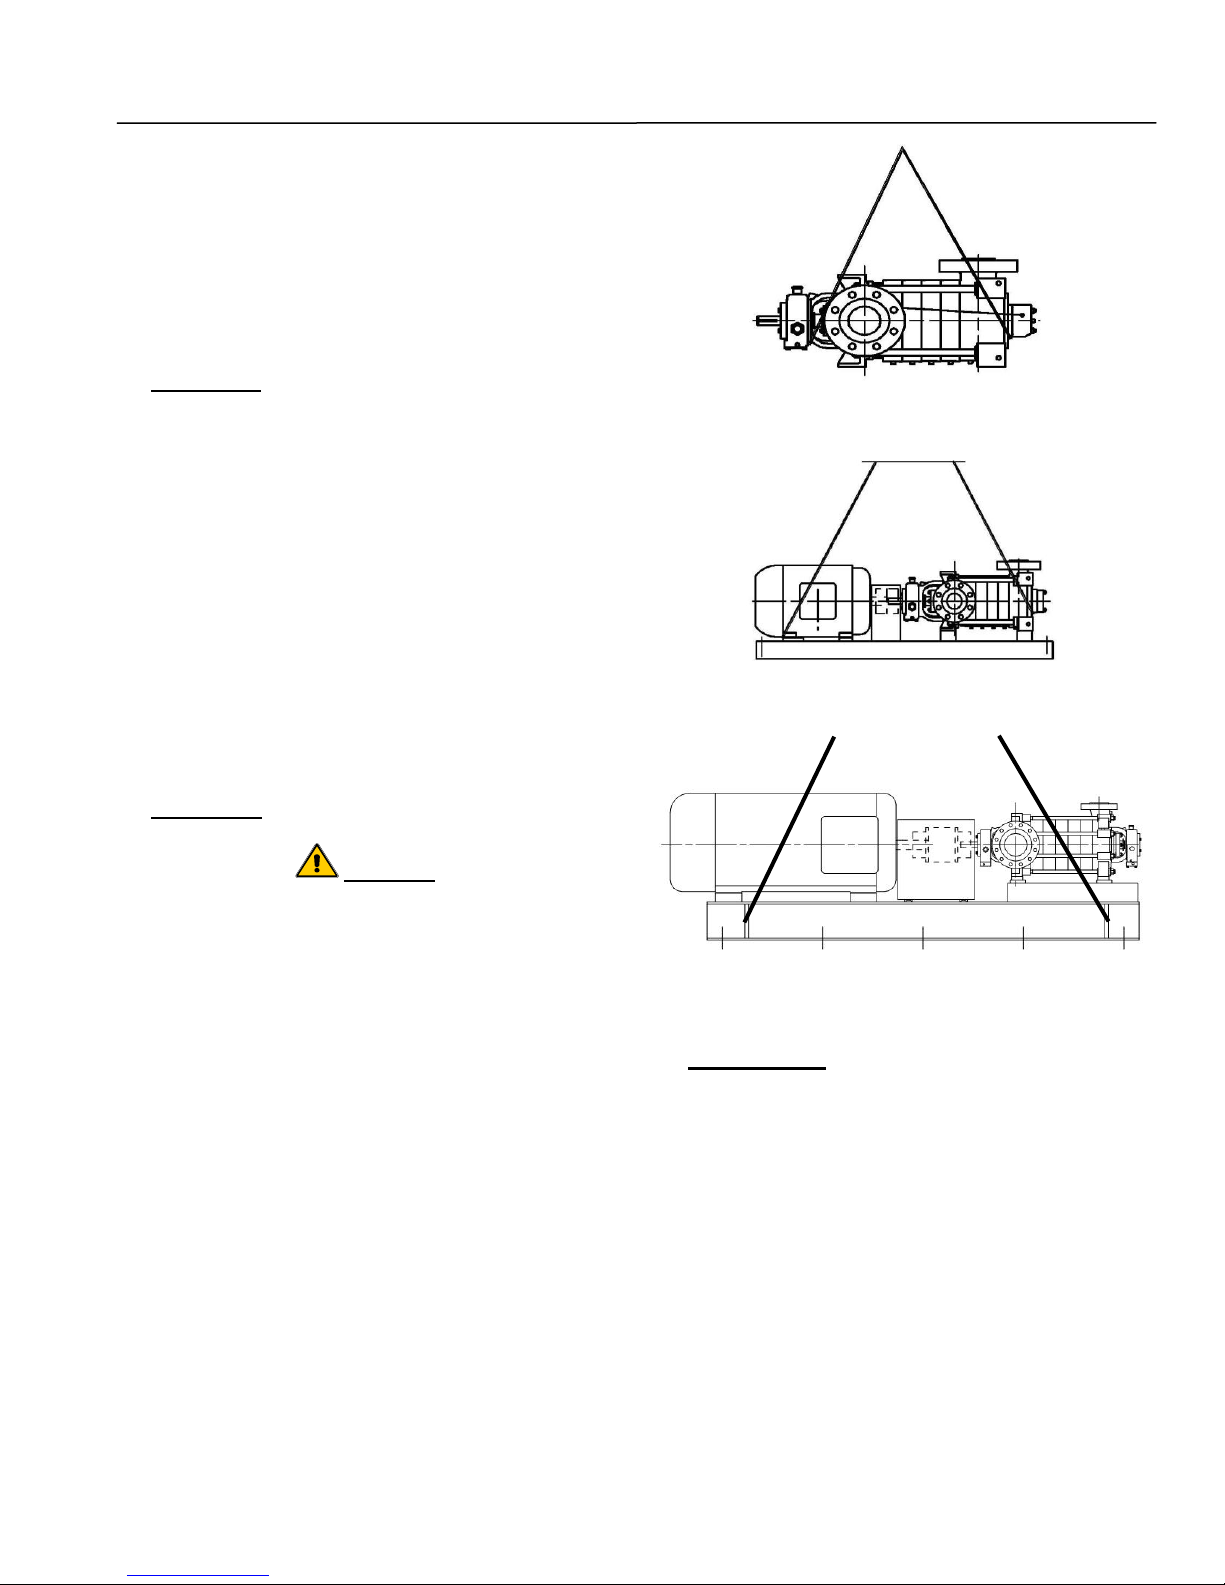
baseplates, refer to Figure 4. To lift a horizontal
mounted unit, a hoist or suitable lifting device should be
attached to each corner of base structure, refer to
Figure 5. To lift a horizontal mounted unit, a hoist or
suitable lifting device should be attached to each lifting
lug on the base structure, refer to Figure 6. The
individual motor may be lifted using proper eyebolts
provided by the manufacturer, but these should not be
used to lift the assembled unit.
Figure 4. Sling Position for Moving Pump
Figure 5. Sling Position for Moving Pumping Unit
Figure 6. Sling Position for
Moving Pumping Unit with Lifting Lugs
C. FOUNDATION. Make sure that the concrete
foundation has set firmly before placing the unit on it. Its
surface must be truly horizontal and even. The
foundation bolts must be inserted in the base holes. The
foundation should be 3 to 6 inches wider and longer
than the base, have a level surface, and be of sufficient
mass to prevent vibration and form a permanent rigid
support for the unit. The best foundations are concrete
with anchor bolts of adequate size embedded in the
foundation in pipe sleeves having an inside diameter 21/2 times larger than the bolt diameter. This will allow for
accurate positioning of the unit. Keep the concrete
surface clean, yet rough.
Hydraulic Institute (HI) recommends a foundation
capable of absorbing vibration at least five times the
weight of the pumping unit and to form a permanent,
17
Page 24
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
rigid support for the base plate. Consequently,
maintaining the pump to driver alignment is important for
a flexible coupled unit, refer to Figure 9. A concrete
foundation on a solid base is recommended. Use
foundation bolts of the proper size embedded into the
concrete. A pipe sleeve larger in diameter than the bolt
should be used. This allows movement for final
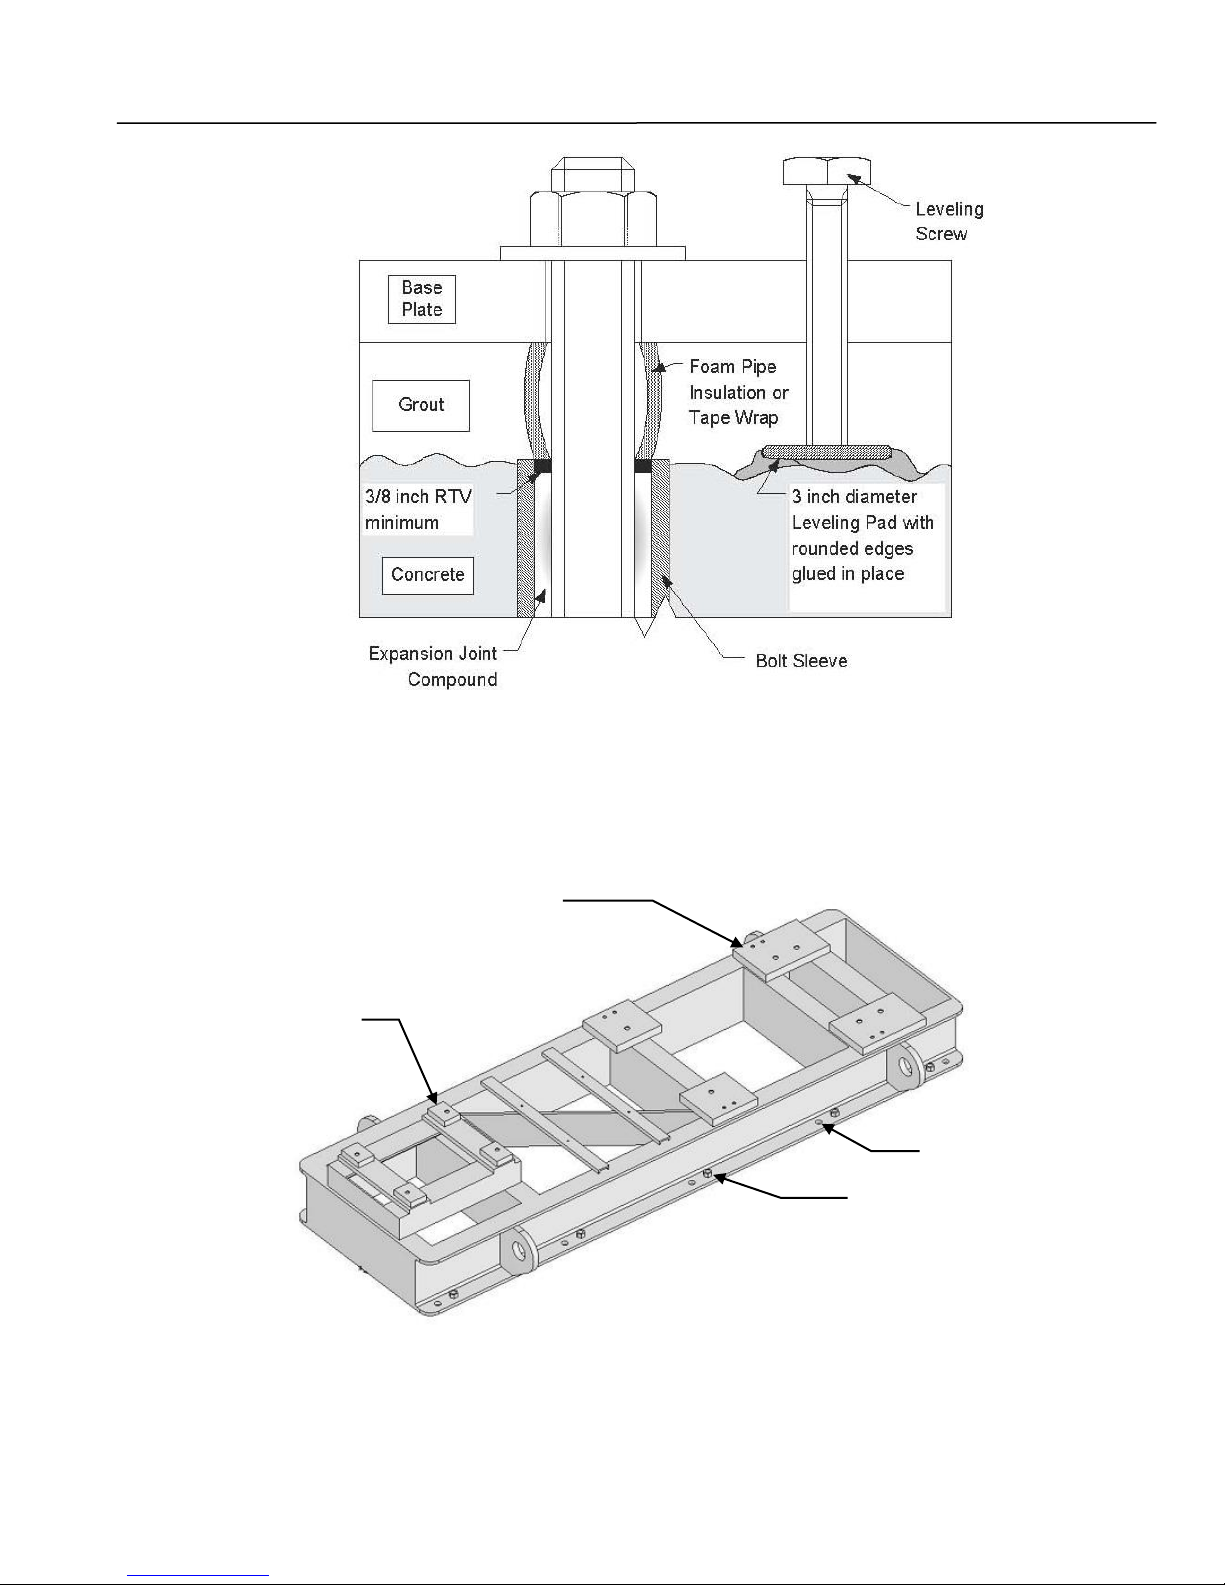
positioning of the bolts; refer to Figure 7, Grouting and
Foundation Bolting.
As soon as the pump and driver, mounted on a base, is
placed on the foundation, remove the coupling guard
and disconnect coupling halves. The base should be
supported by the provided jacking screws. Refer to
Figure 8; adjust the leveling screws until provided base
Verify that the pump and driver shafts are level. Check
coupling faces, as well as, suction and discharge
flanges of the pump for horizontal or vertical positioning
by means of a level. Make corrections, as necessary, by
adjusting the leveling screws on the base.
E. GROUTING. After the pumping unit has been
leveled and the alignment is correct, grout the unit to the
foundation using a high-grade, non-shrinking grout.
Proceed grouting using the following procedure:
Prepare concrete foundations, anchor bolts and leveling
screws according to individual instructions covering
these items.
1. Wax forms heavily with at least three coats of
paste wax. Forms must be substantial and well
braced. All corners, joints, bottoms must be
sealed with silicone caulk for water tightness. All
forms should have a 45° chamfer strip installed
to prevent stress risers.
2. Anchor bolt-free length must be wrapped with
duct seal or electricians plastic tape to prevent
grout from contacting the bare metal. Grout
sticking to the anchor bolt will prevent the
elongation necessary to develop the hold-down
force. Failure to do this will result in broken
D. LEVELING OF UNIT. When the pump is supplied
complete with motor and base, the unit is assembled at
the factory. Lower unit onto foundation, positioning base
structure so anchor bolts are aligned in middle of holes
in base.
The base should be supported on either rectangular
metal blocks with shims or on metal wedges having a
small taper. The support pieces should be placed close
to the foundation bolts, refer to Figure 7, Grouting and
Foundation Bolting. Place supports directly under the
part of the base, which carries the greatest weight.
Space the supports closely enough to provide uniform
support of the base. Adjust the metal supports or
wedges until the shaft is level. Check suction and
discharge flanges of the pump by means of a level.
Make corrections, as necessary, by adjusting the
supports or wedges under the base.
The base should be supported on metal shims or metal
wedges placed directly beneath the part of the base
supporting the most weight. The shims or wedges
should be spaced close enough to give support and
stability.
anchor bolts.
3. If equipped leveling screws must be greased to
permit removal prior to the final torque.
4. Do not use shim packs as a leveling device
unless it is planned to remove them prior to final
torque application.
5. Leveling screw pads should be a minimum of
1/2" thick with minimum diameter of 3". Corners
of pad must be rounded to approximately 1/8"
radius to prevent stress cracking. Set leveling
screws on the chipped concrete surface. Set the
pad with quick set cement or resin repair
compound. With jacking bolt pads secure and
level, set and level base with leveling screws. If
not equipped with leveling screws use shims to
level.
6. The underside of the standard factory steel
base plate was painted with epoxy grout primer
and should only require proper cleaning. If the
base must be sandblasted, prepare the contact
faces to SSPC-SP 6 Spec. If base cannot be set
within 24 hours of blasting, the underside must
be coated with a compatible rust inhibitive
Adjust metal supports or wedges until suction and
discharge flanges are level.
primer. Tighten foundation bolts loosely. Allow
the grout to fully cure before firmly tightening the
foundation bolts.
CAUTION
Do not attempt to straighten the base by using
the anchor bolts.
18
Page 25
RS – Multi-Stage, I-280
Leveling Screw
Anchor Hole
Milled Motor Pad
Milled Pump Pad
(If equipped)
Centrifugal Pump 280 – 16.03.EN
Figure 7. Grouting and Foundation Bolting
Figure 8. Unit Leveling
19
Page 26
RS – Multi-Stage, I-280
Parallel Offset Misalignment
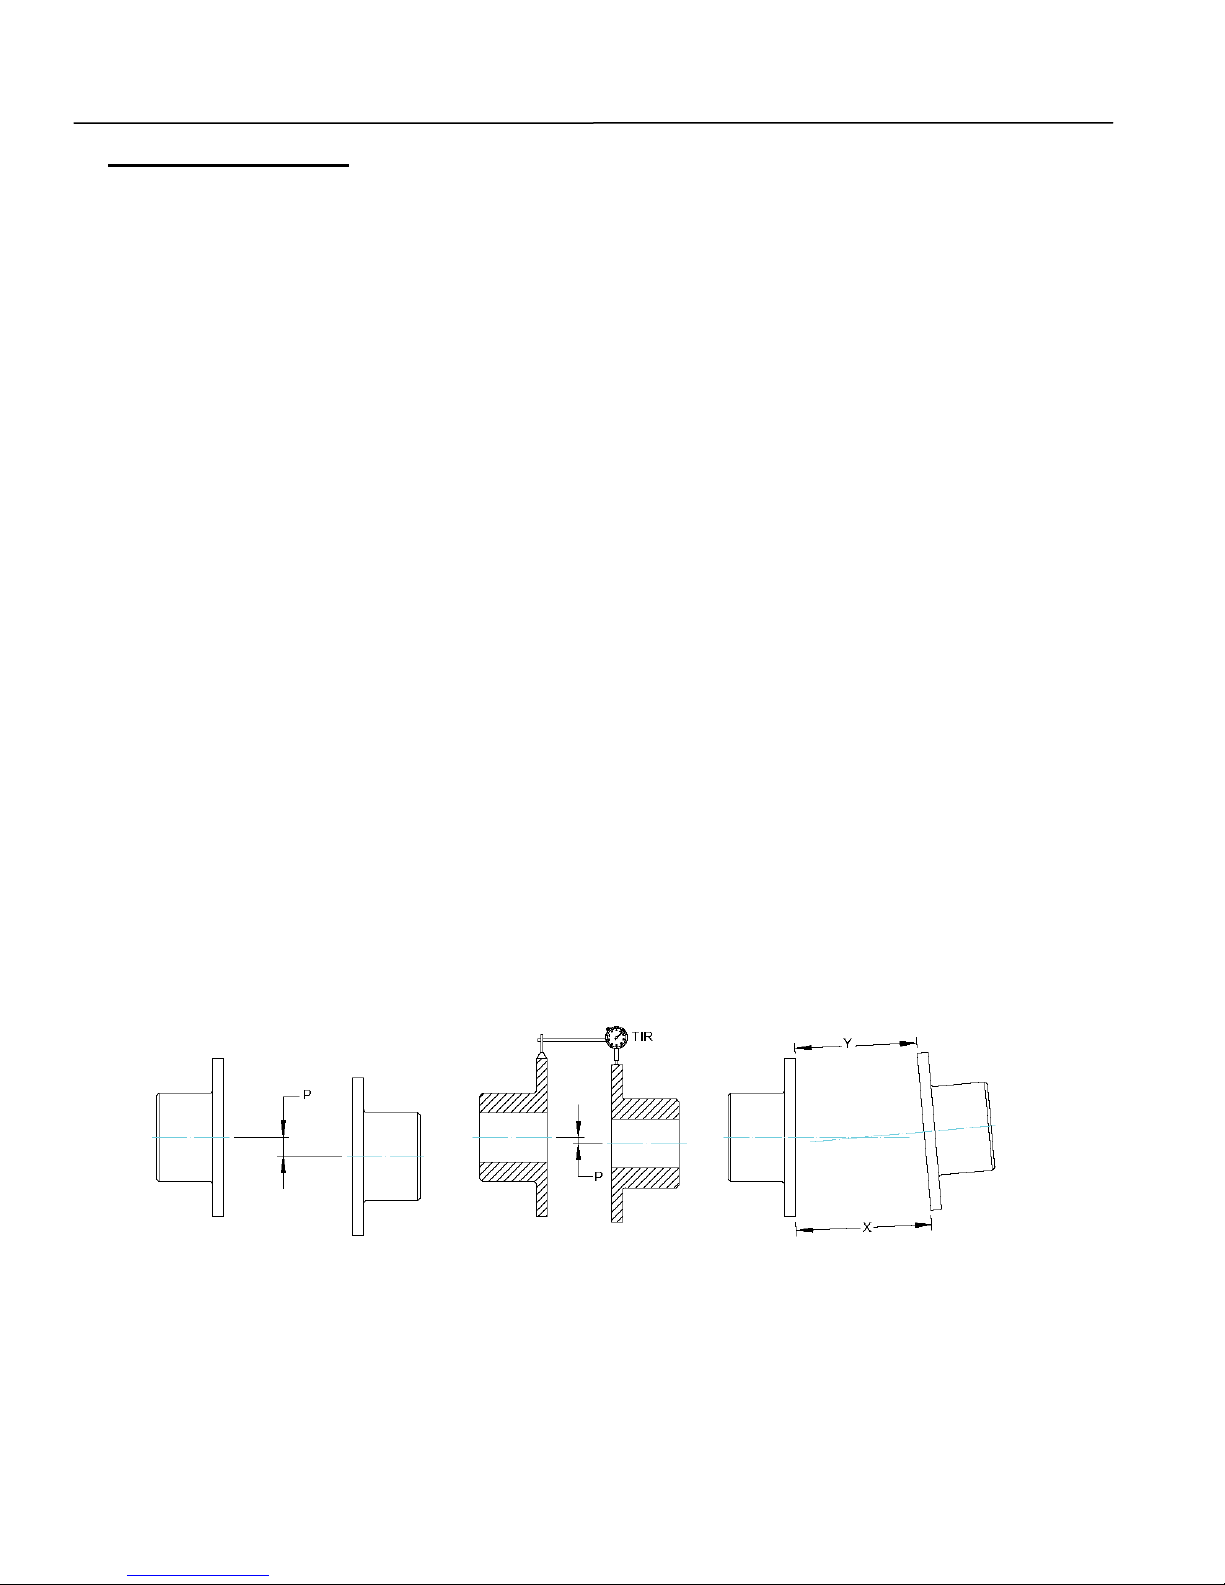
Parallel Offset (TIR)
Measurement
Angular Misalignment
Centrifugal Pump 280 – 16.03.EN
F. COUPLING ALIGNMENT. The pump and motor
are connected by a coupling. Alignment is necessary
when the pump or motor are removed from the base.
The coupling should NOT be reconnected until the
alignment has been completed. Always check the
coupling alignment after shipping. The following is how
to check the coupling alignment.
NOTE
shims under the feet or supports of the motor and
tighten fastening bolts until correct alignment is
achieved.
1. Move the pump or motor to achieve acceptable
alignment. When properly aligned, the disc
packs will be centered and approximately
parallel to their mating flange faces and the
flexing elements will have little visible waviness
when viewed from the side.
Refer to coupling manufacturer’s manual for
instructions regarding shaft alignment and
recommended installation limits.
Soft Foot – The equipment must rest flat on its
base. If one or more feet of the pump or motor
are shorter, longer, or angled in some way to
prevent uniform contact (a condition commonly
known as “soft foot”) it must now be corrected.
To improve the life of the coupling, the shafts must be
aligned to minimize deflection of the flexing elements.
Shaft alignment is required in the axial, parallel, and
angular directions, with each of these values not to
exceed the recommended installation limits. Shaft
alignment can be measured using various established
methods, including Laser Alignment, Reverse Dial
Indicator, and Rim and Face.
The motor and pump shafts must be accurately aligned
as any misalignment can cause damage to the coupling,
motor, or pump. When the shafts are in correct
alignment, the coupling hubs will be on a common axis,
concentric with each other, and at the correct distance
apart. If the coupling hubs are misaligned, it is general
practice to adjust the driver to the pump. Insert full
NOTE
Refer to the coupling manufacturer’s manual for
recommended installation limits for Parallel,
Angular, and Axial alignment.
2. The “Parallel Misalignment” value (P) is the
offset between the centers of the hubs, as
shown in Figure 9.
3. When the Parallel Offset is measured by
rotating the hubs in unison with dial indicators
as shown in Figure 9, the Total Indicator
Reading (TIR) should be divided by (2) to
calculate (P).
4. It should be noted that parallel offset measured
on the hub surfaces includes misalignment of
the equipment shafting plus any variation (TIR)
in the hubs. This may be helpful to consider
during problem solving for alignment difficulties.
5. The “Angular Misalignment” value is the
maximum difference between the
measurements X and Y taken at opposite ends
of the hub flanges, as shown in Figure 9.
20
Figure 9. Coupling Alignment
Page 27
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
G. PRE-INSTALLATION PROCEDURES.
1. Check the pump foundation and confirm the
bolting surface is flat and the bolt pattern is
correct.
2. Slowly lower pump onto the foundation.
3. Rotate the pump by hand. Check for any
mechanical hesitation, binding or any
acoustically transmitted signals from the pump.
Hand rotation should be smooth and silent.
Install the pump to foundation bolting and
tighten to the system torque values. The pump
should be rotated frequently during the
procedure to tighten down the pumping unit.
4. After the pumping unit has been completely
tightened down to the foundation, confirm that
there is no binding.
5. Connect the piping.
H. PIPING. All piping should be independently
supported near the pump so that pipe strain will not be
transmitted to the pumping unit.
CAUTION
All piping connections must be made with the
pipe in a freely supported state. Do not apply
vertical or side pressure to align the piping with
the pump flange.
Before connecting the suction, discharge, and
auxiliary piping, check to see that the piping is
absolutely clean internally. Any debris in the
piping will be drawn into the pump
passageways and can cause extreme damage.
The internal diameters of the suction and
discharge lines must be equal to the internal
diameters of the pump suction and discharge
nozzles.
The pump is shipped with flange covers to protect flange
faces and to prevent foreign matter from entering the
pump. Flange covers should remain intact until suction
and discharge piping are connected to pump flanges.
Suction lift lines shall be laid with a rising slope toward
the pump and suction headlines with a downward slope
towards the pump.
Never use a straight taper (concentric) reducer in a
horizontal suction line because air pockets may form in
the top of the reducer and the pipe. Use an offset
(eccentric) reducer instead.
It is recommended to install a check valve and closing
valve in discharge line and closing valve in suction line,
depending on the type of plant and pump. The check
valve, between the pump and valve, protects pump from
water hammer and prevents reverse rotation in the
event of power failure. Closing valves are used in
priming, starting, and pump shut down. Pump must
never be throttled by use of a valve in the suction line.
Thermal expansions of the pipeline must be
compensated by appropriate measures so as not to
impose any extra loads on the pump exceeding the
permissible pipeline forces and moments. Refer to Table
8 for permissible forces and moments.
The coupling should be realigned after installing piping
or when hot service units are at the final operating
temperature. Refer to Section VII, Paragraph F for
coupling alignment.
I. AUXILIARY PIPING CONNECTIONS AND
GAUGES. In addition to primary piping connections, the
pump may require other connections such as gauges or
drains. All these lines and gauges should now be
installed. Refer to Figure 2 and vendor mechanical seal
drawing for seal line connections to the mechanical seal.
J. MOTOR. See motor vendor’s manual for motor
information and information on connecting to the power
supply.
CAUTION
Connection to the power supply must be
effected by a trained electrician only. Check
available main voltage against the data on the
motor rating plate and select appropriate startup method.
K. DIRECTION OF ROTATION. Correct pump rotation
is indicated by an arrow on the bearing frame. The
standard direction of rotation, viewed from the motor
end, is clockwise.
The suction pipe must be air tight and sloped upward to
pump flange to avoid air pockets which will impair pump
operation. The discharge pipe should be as direct as
possible using a minimum number of valves to reduce
pipe friction losses.
21
Page 28
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
VIII. OPERATION.
A. PRE-START CAUTIONS.
CAUTION
Before activating the pumping unit, check to
make sure there are no personnel working on
the unit. Serious injury or death to personnel
could result if the unit is activated while being
worked on.
1. Before starting or operating the pump, read this
entire manual, especially the following
instructions.
2. Observe all caution or danger tags attached to
the equipment.
CAUTION
7. Jog starter switch on motor to check that the
direction of rotation must agree with the arrow
stamped on the pump frame or base.
8. Before starting the pump, install closed guards
around all exposed rotating parts.
9. If excessive vibration or noise occurs during
operation, shut the pump down and rotate shaft
by hand. If excessive vibration or noise
continues, consult a Carver representative.
B. PRIMING. Dry running a centrifugal pump can
result in extensive damage and possible seizing. It is,
therefore, imperative that the pump be primed prior to
initial start-up and that prime must be maintained
through subsequent start-stop cycles.
The priming procedure is different for positive and
negative suction head systems. Follow the procedure
listed below.
Positive Suction Head:
Pumps are shipped without oil in the
bearing frame and should be filled with oil
before starting the pumping unit. Operation of
the unit without proper lubrication can result in
overheating of the ball bearings, ball bearing
failures, pump seizures and actual breakup of
the equipment, exposing operating personnel to
injury.
3. Fill bearing frame with oil, refer to Section X,
Paragraph A and Table 12. Pumps are shipped
with no oil in the bearing frame.
CAUTION
Never run the pump dry. Close running fits
within the pump are liquid lubricated. Dry
running will result in pump seizure or damage.
4. Before starting the pump, fill the pump and
suction line with liquid. The pump may be
primed by using an ejector or vacuum pump.
5. Before starting a mechanical seal pump
equipped with external flush lines, turn on
mechanical seal water, and confirm the
mechanical seal water is at sufficient pressure.
Refer to Table 13 for minimum cooling flow
rates.
6. Check final alignment of pump and driver. Both
shafts must turn freely by hand. If necessary,
check coupling alignment.
1. Open the vent on the highest point on the pump
casing.
2. Open all suction valves.
3. Allow liquid to flow from vent hole until all air
bubbles are vented. Then close the vent.
4. The pump is now primed.
Negative Suction Head:
1. Install an ejector or vacuum pump on the vent at
the highest point on the casing.
2. Close the discharge valve.
3. Open the suction valve.
4. Start the ejector or vacuum pump.
5. Allow liquid to flow until a continuous flow is
exhausted from ejector. Then close the valve to
the vent.
6. The pump is now primed.
22
Page 29
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
C. STARTING THE PUMP.
surface. If necessary, the minimum flow must be
increased.
CAUTION
Do NOT operate pumping unit against a
closed discharge system. If pump has any
chance of seeing operation against a closed
system, a bypass system allowing a minimum
design flow should be installed. This bypass will
be satisfactory for short periods of operation.
For extended periods of operation the bypass
should be sized for the minimum continuous
flow required by the pump, refer to Table 10.
Refer to Section VIII, Paragraph E for
minimum/maximum flow calculation.
1. Confirm pumping unit is ready to start.
Complete Section VIII, Paragraphs A and B.
2. If unit is equipped with mechanical seal cooling
lines, turn on mechanical seal cooling water.
3. Fully open the suction valve.
4. Open discharge valves slightly, about 1 to 1 ½
turns if pump is being started for the first time or
from being turned off for overhaul. Start the
pump.
5. Slowly open discharge valves and adjust
pressure and flow to the appropriate operating
conditions. Refer to pump nameplate and
system operating procedures for design point
condition.
D. TURBINE APPLICATIONS. For turbine
applications, consult your local distributor or a
representative from Carver Pump Company.
E. MINIMUM/MAXIMUM FLOW CALCULATION.
Unless otherwise specified in the characteristic curves
or on the data sheets, the following applies.
Q
= 0.1 x Q
min
Q
= 0.3 x Q
min
Q
= 1.1 x Q
max
Q
= 1.25 x Q
max
Q
= optimum efficiency
opt
for short operation
opt
for continuous operation
opt
for 2-pole operation
opt
for 4-pole operation
opt
The data above refers to water and water-like liquids.
However, if the physical properties of the fluids handled
are different from water, the calculation formula below
must be used to check if an additional heat build-up may
lead to a dangerous temperature increase at the pump
T o = T f + Δ T
g * H
ΔT = * ( 1 - η )
c * η
c Specific heat [J / kg K]
g Acceleration due to gravity [m/s_]
H Pump head [m]
T f Temperature of fluid handled [°C]
T o Temperature of casing surface [°C]
η Pump efficiency at duty point [ - ]
Δ T Temperature difference [°C]
F. OPERATING CHECKS.
1. Check for undue vibration or noise. If any
occurs and does not stop within a short period
of time, turn off the pump. For determination of
the cause and its remedy refer to
Troubleshooting in Section IX or consult Carver
Pump Company.
2. Check and record flow and pressure readings.
The flow and pressure readings should be
within the operating system guidelines and
similar to number stamped on the pump
nameplate.
3. Check and record power input to the motor.
4. Check for leakage at mechanical seals.
G. STOPPING THE PUMP.
1. If the pump is being stopped for overhaul, slowly
close the discharge valve. Otherwise leave
discharge valves set at condition.
2. Stop the pumping unit in accordance with the
directions on the electrical power supply.
3. Tagout and lockout power to motor according to
OSHA Standard 1910.147.
4. Close discharge and suction valves and any
auxiliary fluid lines.
5. The pumping unit is now off.
23
Page 30
RS – Multi-Stage, I-280
SYMPTOM
PROBABLE CAUSE
CORRECTIVE ACTION
Failure to deliver
liquid.
1. Discharge head above shutoff.
2. Check valve stuck or improperly installed.
3. Impeller or suction line clogged.
4. Improperly installed impeller.
5. Incomplete priming or venting of pump or
piping.
6. Valves are not fully open.
7. Excessive wear of internal parts.
1. Check pump rating against actual head
condition.
2. Adjust and/or reverse valve.
3. Inspect suction line and impeller. Clean as
necessary.
4. Disassemble pump and correct axial
alignment of impeller.
5. Vent piping again carefully and prime
pump.
6. Open valves and if necessary, lock valves
open to prevent accidental closure.
7. Disassemble pump and replace worn parts.
Excessive
power
consumption.
1. Head lower than rating: trying to pump too
much liquid or operating at end of
performance curve.
2. Specific gravity or viscosity of liquid is too
high.
3. Mechanical defects such as binding rotating
elements.
4. System head lower than design condition.
5. Incorrect impeller diameter.
1. Adjust pressure flow.
2. Check liquid temperature and adjust as
necessary.
3. Check for excessive pipe strain. Check
foundation bolting. Replace defective parts.
4. Adjust system head. Trim impellers to
actual condition.
5. Replace impeller or trim impeller to correct
diameter. Consult with Carver Pump before
trimming impellers.
Centrifugal Pump 280 – 16.03.EN
H. INDEFINITE SHUTDOWN.
CAUTION
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
For shipment and long term storage purposes
the pump ball bearing shall be fogged once
every 30 days during storage with a rust
retardant compatible with the oil used in the
system to prevent rusting.
case (111) and suction case (9), and plug (421) from
discharge case (1) depending on design. If necessary,
flush pump to remove corrosive or toxic pumpage.
Collect and dispose of corrosive or toxic material
appropriately. Drain oil from bearing frame by removing
pipe plugs (426) from bearing caps (37). Drain all piping
if there is a possibility of liquid freezing. Provide pump
and driver with a protective cover.
IX. TROUBLESHOOTING OPERATING
PROBLEMS.
If you have followed the installation and starting
procedures outlined in this manual, the pump should
provide reliable service and long life. However, if
operating problems do occur; significant time and
expense can be saved if you refer to Table 11 to
eliminate the most common causes of those problems.
Refer to Figures 13, 14, and 15, for the location of parts
identified by item numbers. Drain pump by removing the
following: plugs (424) form the bottom of each interstage
Table 11. Pumping Unit Troubleshooting
Immediate action to be taken before proceeding with
corrective actions in Table 11 is to stop the pump, refer
to Section VIII, Paragraph G.
24
Page 31
RS – Multi-Stage, I-280
SYMPTOM
PROBABLE CAUSE
CORRECTIVE ACTION
Insufficient
discharge or
flow.
1. Discharge head above shutoff.
2. Air or gases in liquid.
3. Impeller or suction partially clogged.
4. Wrong direction of rotation.
5. Specific gravity or viscosity of liquid is too
high.
6. Incorrect impeller diameter.
1. Check pump rating against actual head
condition.
2. Adjust and/or redesign suction system. Add
liquid to system.
3. Inspect suction and impeller and clean as
necessary.
4. Reverse direction of rotation.
5. Check liquid temperature and adjust as
necessary.
6. Replace impeller or trim impeller to correct
diameter. Consult with Carver Pump before
trimming impeller.
Vibration
excessive.
1. Foundation bolting loose.
2. Coupling halves not properly oriented
relative to each other.
3. Impeller partially blocked.
4. Wrong rotation.
5. Insufficient foundation.
6. Pipe strain.
7. Coupling key to motor or coupling key to
pump is not correct length.
8. Motor improperly balanced.
1. Torque bolting to proper values.
2. Adjust coupling halves system relative to
match marks.
3. Inspect impeller and clean as necessary.
4. Adjust direction of rotation.
5. Stiffen foundation as necessary.
6. Modify piping as necessary.
7. Replace with key of correct length.
8. Balance motor.
Leakage at
casing joints.
1. Tie bolts not sufficiently tightened.
2. O-rings damaged.
1. Release the pressure and tighten the tie
bolts.
2. Replace O-rings.
Oil leak.
1. Loose connection.
2. Defective oil seal.
3. Loose or defective gasket.
1. Tighten connectors.
2. Replace oil seal.
3. Tighten bolting and/or replace gasket.
Bearing
temperature
excessive.
1. Lubrication, insufficient lubrication.
2. Defective ball bearing.
3. Pump/driver shafts are misaligned.
4. Piping causes pump to “warp”.
1. Lubricate according to Section X,
Paragraph A.
2. Replace ball bearing.
3. Check coupling alignment.
4. Ensure piping transmits no stress to pump.
Alter piping layout, if necessary. Realign
pump and driver shafts.
Centrifugal Pump 280 – 16.03.EN
Table 11. Pumping Unit Troubleshooting - Continued
25
Page 32
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
X. MAINTENANCE.
Generally the pump does not need continuous
supervision. The pump should always run quietly and
smoothly, without vibration. To ensure such operation,
the following maintenance schedule should be applied
at regular intervals during operation of the pump.
Occasional visual checks are recommended. Data
should be recorded periodically for each pump to keep
track of maintenance which has been performed and to
note operational problems. A sample maintenance
record sheet is provided for this purpose at the front of
this manual.
Semi-annual Inspection:
Change oil. DO NOT add excess oil.
Check coupling alignment due to settling of
foundation.
If stand-by pumps are installed, it is advisable to
operate pumps on a rotational system to give
each pump a periodic duty. This ensures that
stand-by pumps will have periodic operation and
always be in good condition for instant start-up.
50/300 Hours
The first oil change should be carried out after 50
hours of operation. The second oil change should
be carried out after 300 hours of operation
Regular inspection and service are
essential for safe operation of the pump in
ATEX applications.
NOTE
Parts marked with * are options or vary by
pump or bearing frame size.
Daily Inspection:
Visually inspect unit.
Check bearing cooling flow rates, if applicable,
refer to Table 13.
Check for leakage at mechanical seal.
Check that oil level is at center of bullseye, if
applicable. If equipped with a constant level oiler*,
check oil level in the constant level oiler and refill
as required.
Weekly Inspection:
Check power (amps) readings.
Check pump discharge pressure. Prescribed
operating discharge pressure should never drop
below 90 percent of design point pressure.
Check vibration on pump and driver bearings.
Vibration should NOT exceed 1.5 of overall
displacement (unfiltered) peak to peak mils
(0.001”) at 3600 RPM and 3.0 of overall
displacement (unfiltered) peak to peak mils
(0.001”) at 1750 RPM.
Monthly Inspection:
Check coupling alignment.
If necessary, grease coupling, but DO NOT over
grease.
Check foundation bolts.
1000 Hours
After the second oil change at 300 hours
subsequent oil changes should be effected at
intervals of 1000 hours of operation.
20,000 Hours - Overhaul
For pump overhaul, complete Section XI, Service
and Repair.
A. LUBRICATION OF PUMP BEARINGS.
CAUTION
Pumps are shipped without oil and
bearing frames should be filled with oil before
starting the pumping unit. Operation of the unit
without proper lubrication can result in
overheating of the bearings, bearing failures,
pump seizures and actual breakup of the
equipment, exposing operating personnel to
injury.
Ball Bearings (16 and 18). The radial ball bearing and
the thrust ball bearings are lubricated by oil in the
bearing frame. The thrust ball bearings are installed
back to back. Replace the ball bearings when
disassembling the pumping unit for mechanical seal
service. Refer to Figures 13, 14, and 15, for the location
of parts identified by item numbers.
Fill the bearing frame (99) with oil (refer to Table 12 for
oil recommendations) through the breather vent (405)
until oil can be seen in the center of the oil view sight
(143)*.
To change oil, unscrew oil cap pipe plug (425) in
bearing caps (35 and 37) and drain oil. Flush bearing
frame with petrol or benzol. Slowly rotate the shaft by
hand during flushing. Replace oil cap pipe plug and fill
26
Page 33
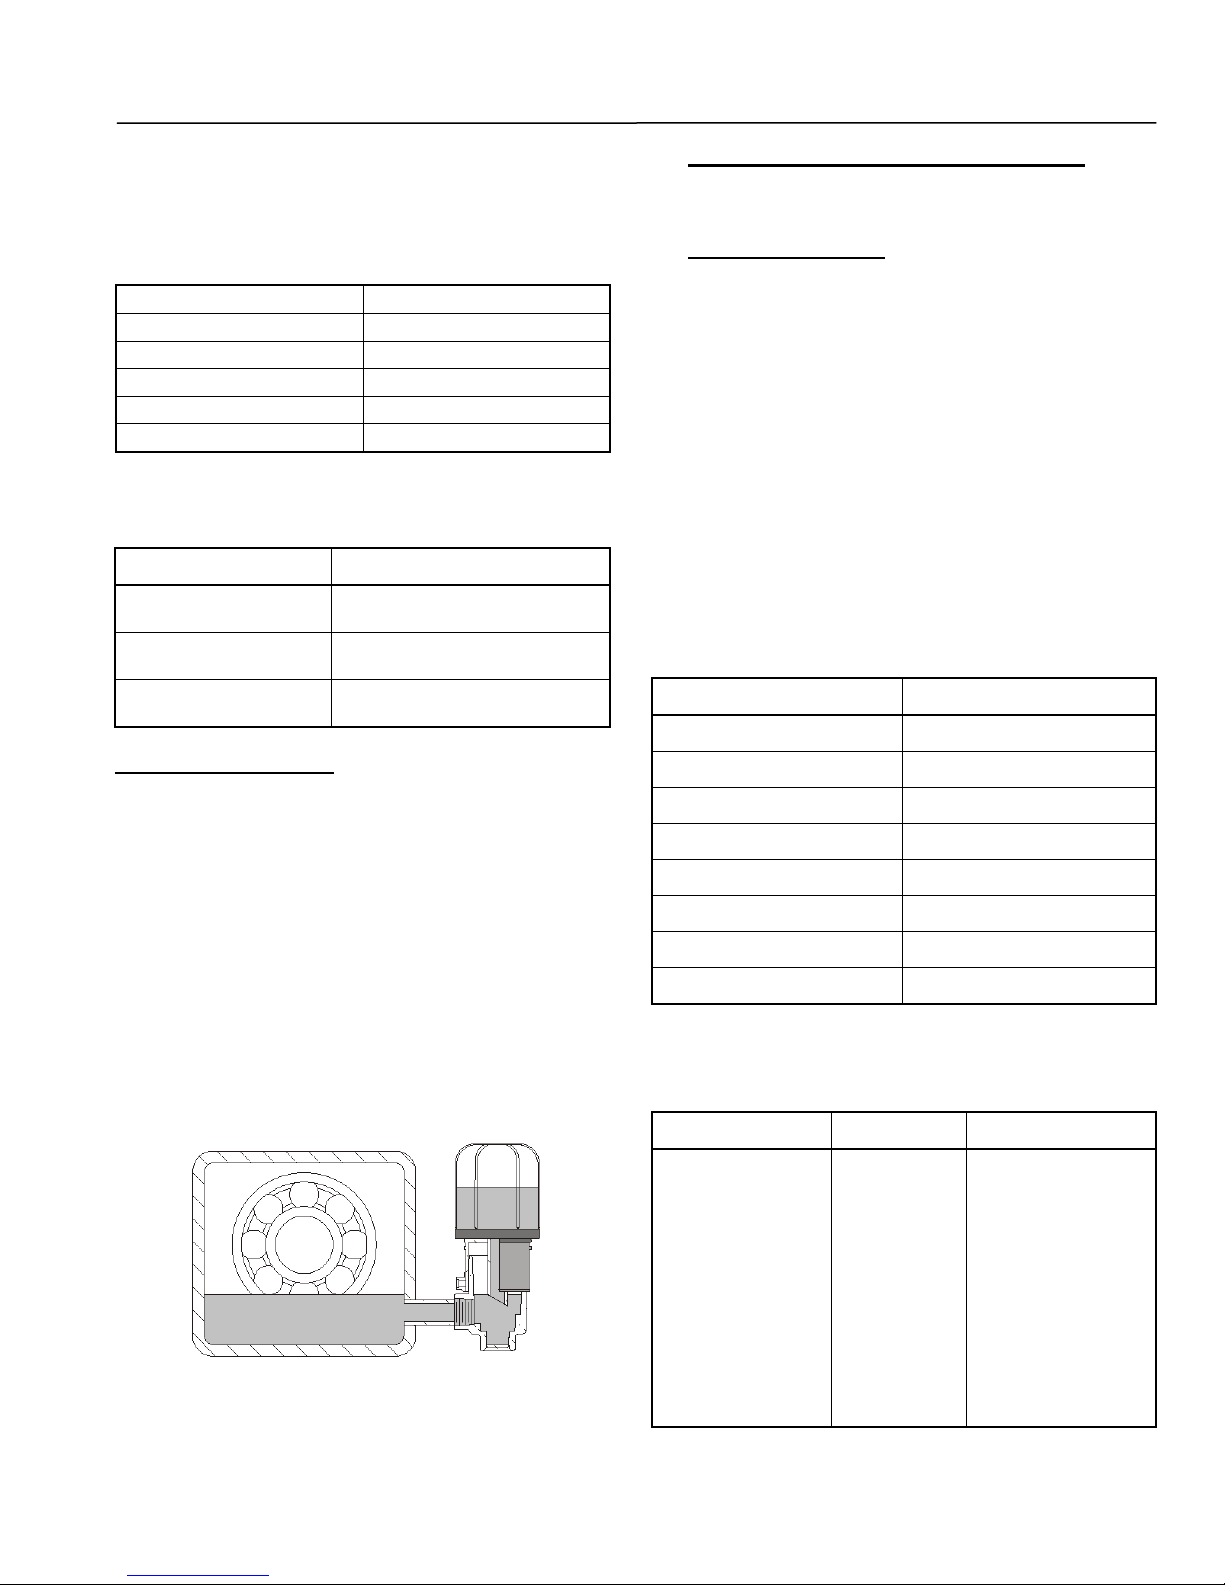
RS – Multi-Stage, I-280
Manufacturer
ISO Grade 68
Royal Purple
Synfilm 68
Texaco
Regal R&O 68
Phillips
Magnus Oil 68
Exxon
Teresstic 68
Mobil
DTE 16 M
Temperature Range
Flow Rate
-20˚ to 225˚ F
(-4° to 107° C)
Oil Lube - Air
225˚ to 285° F
(107° to 140° C)
Oil-Lube – Water
1 Gallons per Minute (GPM)
285˚ to 300° F
(140° to 148° C)
Oil-Lube – Water
2 GPM
Fastener Size
Torque Value
1/4-20 UNC
5
5/16-18 UNC
10
3/8-16 UNC
15
1/2-13 UNC
30
Bearing Jam Nuts
3/20/30*
RS6-A, B, C, D Tie Rod*
160
RS9-A, B, C, D Tie Rod*
315 / 50 ft-lbs increments
RS9-E Tie Rod*
446 / 50 ft-lbs increments
*(Refer to Section X, Paragraph C)
Tools
Materials
Test Equipment
Spanner Wrench
Rawhide or
Wood Mallet
Oil
O-ring
Lubricant
Coupling
Alignment
Gauges
Wooden Wedge
Volt-Amp Meter
Allen Wrench Set
Socket, Open, &
Box Wrench
Set
Vice Grips
Torque Wrench
Jam Nut Wrench
Centrifugal Pump 280 – 16.03.EN
the bearing frame (99) with oil (refer to Table 12 for oil
recommendations) through the breather vent (405) until
oil can be seen in the center of the oil view sight (143)*.
B. LUBRICATION OF MOTOR BEARINGS. See
motor manufacturer’s instructions to be sure motor
bearings are properly lubricated.
Table 12. Oil Recommendations
Table 13. Bearing Cooling Flow Rates
(30 PSIG MAX.)
*Constant Level Oiler. If equipped with a constant
level oiler, fill reservoir with oil, place thumb over spout,
invert and screw reservoir into upper casting. Allow
reservoir to empty, filling the bearing frame (Figure 10).
Several fillings of the reservoir may be required before
the actual oil level is reached. To avoid adding too much
oil, never finish filling oil in bearing frame (99) through
the vent breather (405) at top of the bearing frame.
Never use lower casting only as a fill spout, always fill
thru reservoir. When oil level is reached, no more oil will
run out of the reservoir bottle. Use constant level oiler's
glass sight to check oil level in bearing frame. When oil
level is reached tighten the three setscrews on the side
of the upper oiler. The constant level oiler (143) should
be topped up as required during operation.
C. TORQUE VALUES. Refer to Table 14,
Recommended Torque Values. Clean and properly
lubricate threads and bearing face of the fastener to
obtain the proper fastener loading from these torque
values. Fasteners should be tightened evenly and in
stages with a criss-cross bolt pattern. Refer to your
torque wrench manual for the proper use of your
wrench.
Refer to the pump nameplate to determine your pump
model for tie rod torques.
The first bearing jam nut (22) is to have 20 ft-lbs torque
while holding the coupling end of the shaft. The second
bearing jam nut is to be tightened to 30 ft-lbs while
holding the coupling end. Loctite the second bearing jam
nut.
Table 14. Recommended Torque Values (ft-lbs)
Table 15. Recommended Equipment
Figure 10. Constant Level Oiler
27
Page 34
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
XI. SERVICE AND REPAIR.
CAUTION
Refer to Figures 13, 14, and 15 to locate the pump parts
by item number and parts list.
A. PREPARATIONS FOR DISASSEMBLY OF PUMP.
During disassembly, match mark parts so they can be
replaced in their original position. All parts should be
thoroughly cleaned or replaced with new, if necessary.
Sealing faces should be perfectly clean.
CAUTION
Factory authorized parts must be used to
safely maintain your Carver Pump.
NOTE
To avoid damage to O-rings, check to make
sure all parts are free of sharp edges or burrs.
Parts marked with * are options or vary by
pump or bearing frame size.
O-rings, ball bearings, oil seals/bearing
isolators, mechanical seals and gaskets if
disturbed from position should be replaced.
Close suction and/or discharge valves. The pump
should be cooled down to ambient temperature. The
casings must be empty and not under pressure.
After prolonged operation, components may not be
easily removed from shaft. In such instances, rust
solvent may be used and suitable extracting tools
applied wherever possible. DO NOT use force under
any circumstances. Refer to Table 15, Recommended
Equipment, for proper tooling during disassembly and
assembly. Refer to appropriate sectional drawing for
location of parts followed by an item number.
Prepare the pumping unit for disassembly using the
following list:
1. Read this entire section and study the
applicable sectional view drawing and parts list
before disassembling the pump.
2. Stop the pumping unit; refer to Section VIII,
Paragraph G.
Before attempting to disassemble the pump,
the electrical power supply to the driver must
be locked and tagged in the “OFF” position to
prevent injury or death to personnel servicing
the pumping unit.
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
3. For cartridge mechanical seals (90* or 91*),
reinstall seal clip.
4. Disconnect piping, gauge lines, and auxiliary
connections, as necessary.
5. Drain pump by removing the following plugs:
plug (424) form the bottom of each interstage
case (111) and suction case (9), and plug (421*)
from discharge case (1). If necessary, flush
pump to remove corrosive or toxic pumpage.
Collect and dispose of corrosive or toxic
material appropriately.
6. Drain oil from bearing frame by removing pipe
plugs (426) from bearing caps (37 and 37A*).
7. Confirm water from the oil cooler (215A*) is
drained.
8. Disconnect all male connector retaining nuts
from male connectors (410 and 561*) bodies, as
applicable. Remove tubing (400 and 401), as
applicable. Retaining nuts will remain with
tubing.
9. Remove coupling guard and disconnect
coupling halves.
10. Remove nuts and washers, as applicable from
discharge (1) and suction casing feet (9) holding
pump to base. Move the pump to a suitable
work area for disassembly; refer to Section VII,
Paragraph B for handling of the pump.
28
Page 35
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
B. DISASSEMBLY OF PUMP WITH STANDARD
SLEEVE BEARING. The instructions that follow are an
aid for properly trained personnel to service your Carver
Pump. Refer to Figures 13 and 15 to locate the pump
parts by item number and parts list. If a specific
sectional assembly drawing exists for a particular job
then that drawing should be referred to for service work.
Read this entire section before disassembling the pump.
NOTE
Parts marked with * are options that vary by
pumping unit and bearing frame size.
4. Starting on the discharge side (Outboard)
remove gland nuts (615) and gland washers
(646) from the outboard bearing cap stud (631).
Remove outboard bearing cap (37A) from the
discharge case (1). Remove the gland O-ring
(89H) from the outboard bearing cap.
5. Remove male connector (410) body from the
seal gland (17A).
6. Remove hex nuts (615) and gland washer (646)
from studs (630) on seal gland (17A). Slide back
the seal gland from suction case (9) to release
mechanical seal (90) tension.
7. Remove tie bolt nuts (616) and tie bolt washers
ATEX and CE require bearing isolators and
metal splash guards. Other customers may use
oils seals and plastic splash guards. These
items fit in the same positions.
(645). Remove tie bolts (173) connecting the
discharge case (1) and the suction case (9).
8. Remove jam nuts (614) and shaft washer (28)
from shaft (6).
Refer to Section II for Safety precautions before
disassembling pump.
CAUTION
After completion of dismantling, all parts should be
thoroughly cleaned or replaced by new ones if
necessary. All gaskets and sealing faces should be
perfectly clean. When cutting new gaskets, make sure
they are exactly the same thickness as the old ones.
CAUTION
Use a hoist with adequate lifting capacity; refer
to Section VII, Paragraph B.
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
NOTE
Pump should be dismantled from the discharge
end. Mark or number each component while
dismantling according to sequence.
1. Complete Section XI, Paragraph A before
continuing with disassembly.
2. With pump in a horizontal position clamp down
suction case (9) foot to steady pump during
disassembly.
3. Support interstage casings (111) before
dismantling to prevent from being dropped while
discharge case (1) is removed.
Use a hoist with adequate lifting capacity for
lifting the discharge case (1).
NOTE
The last stage bushing (63X), O-ring (89A), and
the last stage diffuser (5X) with wear ring (7X)
still intact will come off with the discharge case.
Match mark impellers, sleeves, keys, interstage
casings and casings according to sequence.
9. Remove discharge case (1) with sleeve bearing
(63Y) still intact.
10. Remove the last stage diffuser (5X) with wear
ring and last stage bushing (63X) still intact.
Remove O-ring (89A) from the last stage
bushing.
NOTE
Refer to Table 5, Sleeve Bearing Dimensions to
determine if replacement of sleeve bearing
(63Y) is required.
IMPORTANT: Check for shims between
impellers and spacer sleeves.
11. If replacing sleeve bearing (63Y), remove
sleeve bearing from discharge case (1).
12. Remove sleeve (14X) from shaft.
13. Remove impeller (2X) and impeller key (32A)
from shaft.
14. Remove interstage casing (111) with casing Oring (89D), diffuser (5A), diffuser bushing (63)
29
Page 36
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
and wear ring (7X) intact. Remove casing O-ring
from interstage casing and discard O-ring.
15. Remove impeller key (32A). Remove interstage
Refer to mechanical seal vendor instructions for
proper mechanical seal removal procedure.
NOTE
sleeve (58). Remove interstage shims (73G), as
necessary, from both sides of interstage sleeve.
Record the location of all removed shims for
ease of assembly.
16. Repeat steps 14 and 15 for each stage of the
DO NOT remove rotating element of
mechanical seal (90) from shaft sleeve (14A) at
this point, especially if mechanical seal is
relatively clean and in good working condition.
pump. Number and match mark all parts during
removal.
17. Remove the spacer sleeve (14D).
26. For Type 1 mechanical seals (90*), remove
gland (17A) from shaft (6).
27. Remove sleeve (14A) and rotating element of
NOTE
Before removing wear rings from casings
inspect per Section XI, Paragraph D, step 9.
Wear rings should only be removed for
replacement, refer to Section XI, Paragraph G
for wear ring replacement.
mechanical seal (90*) from shaft (6). Inspect
rotating element of mechanical seal. If
replacement is required, remove element from
sleeve.
28. Remove O-ring (89X).
29. If necessary to replace mechanical seal (90*),
remove stationary element of mechanical seal in
18. If replacement is required, remove wear ring
(7X) and diffuser (5X). First wear ring (7A) will
remain in the suction case (9) unless
replacement is required.
19. Remove casing O-ring (89D) from suction case
(9) and discard casing O-ring.
seal gland (17A). Remove gland O-ring (89H)
from seal gland and discard O-ring.
30. For cartridge mechanical seals (90*), loosen
setscrews holding the cartridge seal sleeve to
shaft (6). Remove cartridge seal from shaft.
31. Remove key (32X) from shaft (6).
NOTE
Shaft (6), mechanical seal (90), seal gland
(17A), bearing cap bearing isolator (168*),
bearing frame bearing isolator (169*), and
inboard bearing cap (37) will come off together
with the bearing frame (99) as an assembly.
20. Remove bolts (600) from bearing frame (99).
Remove bearing frame assembly from suction
case (9).
21. Remove bolts (601), washer (850), O-ring
(89W), and remove inboard bearing cap (37).
Remove bearing cap bearing isolator (168*)
from inboard bearing cap and discard bearing
cap bearing isolator.
22. Remove bearing jam nuts (22) from shaft (6).
23. Remove back-to-back ball bearings (16) with
bearing frame (99) from shaft (6).
24. Remove bearing spacer (78) with slinger (40)
intact, from shaft (6). Remove bearing frame
bearing isolator (169*) from bearing frame (99)
and discard bearing frame bearing isolator.
25. Remove snap ring (176).
NOTE
DO NOT remove seal collar (68), unless sleeve
(14A) needs replaced.
32. Remove setscrews (665) from seal collar (68).
Remove seal collar from sleeve (14A).
30
Page 37
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
C. DISASSEMBLY OF PUMP WITH OPTIONAL
MECHANICAL SEALS. The instructions that follow are
4. Remove male connectors (410 and 561*)
bodies from seal glands (17A and 17X*).
an aid for properly trained personnel to service your
Carver Pump. Refer to Figures 14 and 15 to locate the
pump parts by item number and parts list. If a specific
sectional assembly drawing exists for a particular job
then that drawing should be referred to for service work.
Read this entire section before disassembling the pump.
NOTE
Parts marked with * are options that vary by
pumping unit and bearing frame size.
Refer to mechanical seal vendor instructions for
proper mechanical seal removal procedure.
5. For cartridge mechanical seals (90*), loosen
setscrews holding the cartridge seal sleeve to
shaft (6) and remove cartridge seal.
6. For Type 1 mechanical seals (90*), remove nuts
(615) and washers (646) from studs (630) on
NOTE
seal glands (17A and 17X). Slide back seal
ATEX and CE require bearing isolators and
metal splash guards. Other customers may use
oils seals and plastic splash guards. These
items fit in the same positions.
Refer to Section II for Safety precautions before
disassembling pump.
After completion of dismantling, all parts should be
thoroughly cleaned or replaced by new ones if
necessary. All gaskets and sealing faces should be
perfectly clean. When cutting new gaskets, make sure
gland from suction casing (9) and discharge
casing (1) to release mechanical seals (90 and
91) tension.
7. Starting on suction end (Inboard) remove bolts
(601), washers (850), O-rings (89W) from
bearing cap (37). Remove bearing cap (37) from
inboard bearing frame (99). Bearing cap bearing
isolator (168*) will be removed with bearing cap.
Remove bearing cap bearing isolator and
discard.
8. Remove bearing jam nuts (22) from shaft (6).
they are exactly the same thickness as the old ones.
NOTE
CAUTION
Do not remove both bearing frames at the
same time. Pump should be dismantled from
Use a hoist with adequate lifting capacity; refer
the suction end.
to Section VII, Paragraph B.
9. Remove bearing frame bolts (600). Remove
inboard bearing frame (99) from suction case
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
(9). Ball bearing (16), spacer sleeve (14G), and
bearing frame bearing isolator (169) will come
off together with the inboard bearing frame.
Discard ball bearing and bearing frame bearing
isolator.
10. Remove slinger (40) from sleeve (14A).
Remove seal gland (17A) and sleeve from shaft
NOTE
(6).
Pump should be dismantled from the suction
end. Mark or number each component while
dismantling according to sequence.
1. Complete Section XI, Paragraph A before
continuing with disassembly.
2. With pump in a horizontal position clamp down
discharge case (1) foot to steady pump during
disassembly.
3. Support interstage casings (111) before
dismantling to prevent from being dropped while
suction case (9) is removed.
31
Page 38
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
NOTE
NOTE
DO NOT remove rotating element of
mechanical seal (90*) from sleeve (14A) at this
point, especially if mechanical seal is relatively
clean and in good working condition.
11. If necessary to replace mechanical seal (90*),
remove stationary element of mechanical seal in
seal gland (17A). Remove gland O-ring (89H)
from seal gland and discard O-ring.
12. For Type 1 mechanical seals (90*), remove
sleeve (14A) with rotating element of
mechanical seal (90*) from shaft (6). Inspect
rotating element of mechanical seal. If
replacement is required, remove rotating
element from sleeve.
13. Remove tie bolt nuts (616) and tie bolt washers
(645) from tie bolts (173). Remove tie bolts
connecting the suction case (9) and the
discharge case (1).
CAUTION
Use a hoist with adequate lifting capacity for
lifting the suction case (9).
NOTE
Mark or number each component while
dismantling according to sequence.
14. Remove suction casing (9). Remove sleeve key
(32X) from shaft (6).
NOTE
Before removing wear rings from casings
inspect per Section XI, Paragraph D, step 9.
Wear rings should only be removed for
replacement, refer to Section XI, Paragraph G
for wear ring replacement.
15. First wear ring will remain in the suction case
unless replacement is required. If replacement
is required, remove first wear ring (7A) from
suction case (9).
16. Remove casing O-ring (89D) from suction
casing (9) and discard O-ring.
IMPORTANT: Check for shims between
impellers and spacer sleeves.
17. Remove sleeve O-ring (89X) from shaft (6) and
discard O-ring. Remove spacer sleeve (14D)
and first impeller (2A) from shaft.
18. Remove interstage case (111) with diffuser
(5A), wear rings (7B and 7X), diffuser bushing
(63), and casing O-ring (89D) intact. Remove Oring from interstage case and discard O-ring.
NOTE
Before removing wear rings from casings
inspect per Section XI, Paragraph D, step 9.
Wear rings should only be removed for
replacement, refer to Section XI, Paragraph G
for wear ring replacement.
19. If replacement is required, remove wear rings
(7B and 7X) and diffuser (5A).
20. Remove impeller key (32A) and interstage
sleeve (58) from shaft (6). Remove interstage
shims (73G), as necessary, from both sides of
interstage sleeve (58). Record the location of all
removed interstage shims for ease of assembly.
21. Remove interstage impeller (2X) from shaft (6).
22. Repeat steps 18 through 21 for each stage of
the pump. Number and match mark impellers
during removal.
NOTE
The last stage diffuser (5X), wear rings (7B and
7X), the last stage diffuser bushing (63X), and
O-ring (89A) will come from the discharge
casing together with the last stage diffuser.
23. Remove last stage diffuser (5X) from the
discharge case (1). Remove O-ring from last
stage diffuser bushing and discard O-ring.
Remove spacer sleeve (14E) from shaft (6).
24. Remove bolts (600) from bearing frame (99)
and discharge case (1).
NOTE
Shaft (6), mechanical seal (91*), seal gland
(17X*), bearing cap (37), ball bearings (18),
and bearing frame bearing isolators (169) will
come off with outboard bearing frame (99).
32
25. Remove bearing frame (99) assembly.
Page 39
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
26. Remove bearing cap bolts (601), bearing cap
bolt washers (850), and bearing cap bolt O-ring
(89W) from bearing cap (37) and discard O-ring.
Remove bearing cap (37).
rings, oil seals/bearing isolators, and locking
devices with a nylock feature are to be replaced
with new if disturbed from position.
3. Check shaft for runout, scratches, grooves, or
any possible damage. Touch up scratches and
NOTE
If ball bearings and/or oil seals/bearing isolators
are disturbed from position replace with new.
grooves with a polishing cloth and inspect for
remaining grooves or deep scratches. A bent or
excessively damaged shaft should be replaced.
4. Inspect the discharge, interstage and suction
27. If necessary to remove back-to-back ball
bearings (18), remove bearing jam nuts (22)
from shaft (6).
28. Remove back-to-back ball bearings (18) and
bearing frame bearing isolators (169*) with
outboard bearing frame (99) from shaft (6).
Discard bearing frame bearing isolators.
29. Remove bearing spacer (78) from shaft (6).
30. Remove snap ring (176) from shaft (6). Remove
slinger (40X) from sleeve (14X).
NOTE
Refer to mechanical seal vendor instructions for
proper mechanical seal removal procedure.
casings for pitting, scoring, and erosion. The
inside of the discharge, interstage and suction
casings should be free of any pits or grooves.
The maximum allowable depth is 1/8” (3mm).
Replace the discharge, interstage or suction
casings if any of these defects are present.
5. Inspect mechanical seal. Replace the
mechanical seal that is disturbed from position
or damaged.
6. Inspect impeller, sleeve, and coupling keys for
distortion and push fit into keyways. The keys
should be square on all four edges. They should
fit without having to be forced. The keys should
not rock in keyway. Replace keys or shaft if
necessary.
7. Inspect tubing for kinking. Replace kinked
DO NOT remove rotating element of
mechanical seal (91*) from shaft sleeve (14X)
at this point, especially if mechanical seal is
relatively clean and in good working condition.
31. For cartridge mechanical seals (91*), loosen
setscrews that hold the cartridge seal sleeve to
seal sleeve (14X) and remove cartridge seal.
32. For Type 1 mechanical seals (91*), remove seal
gland (17X).
33. If necessary to replace mechanical seal (91*),
remove stationary element of mechanical seal in
seal gland (17X). Remove gland O-ring (89H)
from seal gland.
34. Remove sleeve (14X) and rotating element of
mechanical seal (91*) from the shaft (6). Inspect
rotating element of mechanical seal. If
replacement is required, remove rotating
element from sleeve.
35. Remove key (32X) from shaft (6).
D. PARTS INSPECTION.
tubing.
8. If the impeller shows excessive wear due to
erosion or pitting, so that performance cannot
be restored, it must be replaced. If a new
impeller is installed, check to make sure that it is
balanced and of the correct trim. If an impeller is
restored or replaced, check the dynamic
balance of the rotor before reassembly of the
pump.
9. Check the wear ring clearance as follows:
a. Measure outside diameter of front impeller
hub (2A or 2X) in three places.
b. Measure inside diameter of wear ring (7A)
in three places.
c. If difference between the high reading of the
inside diameter of the wear ring (7A) and
the low reading of the outside diameter of
the impeller (2A or 2X) wear ring exceeds
double the new maximum clearances given
in Table 16, replace the wear ring according
to Section XI, Paragraph G.
d. Measure outside diameter of back impeller
1. All parts should be thoroughly cleaned with a
suitable solvent or replaced with new ones if
necessary.
2. All sealing faces should be perfectly clean. All
ball bearings, mechanical seals, gaskets, O-
hub (2A or 2X) in three places.
e. Measure inside diameter of the back wear
ring (7X) in three places.
f. If difference between the high reading of the
inside diameter of the back wear ring (7X)
33
Page 40
RS – Multi-Stage, I-280
Pump Size
New Maximum
Diametrical Clearance
(Casing & Diffuser)
A
0.030
B
0.030
C
0.024
D
0.022
E
0.026
Centrifugal Pump 280 – 16.03.EN
and the low reading of the outside diameter
of the back impeller (2A or 2X) wear ring
exceeds double the new maximum
clearances given in Table 16, replace the
back wear ring according to Section XI,
Paragraph G.
h. Check rotor TIR by placing an indicator on
the impeller wear ring wearing surface and
the interstage sleeves (58), rotate the shaft
(6) slowly for reading. Rotor TIR must be
.006 inch or less. Check coupling end of
shaft to verify less than .003 inch TIR.
i. To achieve the best TIR, loosen the jam nut
10. Check rotor TIR and balance as follows:
a. Check shaft TIR on roller bearing “V” blocks
in (3) spots, coupling end, middle and
discharge end of shaft.
b. Install O-ring (89X) on suction end for
standard design or discharge end for
optional design. Install key (32X). Install the
sleeve (14A, standard design or 14X,
optional design).
c. Install snap ring (176). Install bearing
spacer (78). Install ball bearings (16,
standard design or 18, optional design)
back to back, meaning lettering on the outer
race facing each other.
d. Install first bearing jam nut (22) and torque
(614, standard design), rotate shaft (6) 90
degrees, torque jam nut and recheck and
record all TIRs again. When best TIR has
been achieved, mark both ends of shaft with
an arrow pointing down.
j. Tape ball bearings (16, standard design or
18, optional design) so they don’t spin on
shaft (6) and are covered so no debris gets
in during the balancing of the rotor.
k. Dynamic balance rotor to G-6.3 spec.
l. IMPORTANT: Mark all impellers, sleeves,
interstage sleeve gaskets, and keys with
numbers in the order they were staged
while dismantling according to sequence for
rotor balbance. Disassemble rotor.
to 3 ft/lbs. Install second bearing jam nut
and torque to 30 ft/lbs. making sure that the
Table 16. Factory Wear Ring Clearance (Inches)
first bearing jam nut does not tighten with
the second bearing jam nut.
e. Install spacer sleeve (14D, standard design
or 14E, optional design) on shaft (6).
f. Install impeller (2A, standard design or 2X,
optional design). Install the interstage
sleeve (58) on the shaft (6). Repeat until
you have no more impellers to put on the
shaft.
g. Install sleeve (14X) on shaft (6). Install shaft
washer (28, standard design) on shaft and
first jam nut (614, standard design), torque
jam nut to 30 ft/lbs. Note where the coupling
shaft keyway is oriented. This is important
to getting the best rotor TIR.
34
Page 41
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
E. REASSEMBLY OF PUMP WITH STANDARD
SLEEVE BEARING. Read this entire section before
4. Slide bearing spacer (78) onto end of shaft.
Install slinger (40) on bearing spacer.
reassembling the pump. The instructions that follow are
an aid for properly trained personnel to assemble your
Carver Pump. Refer to Figures 13 and 15 to locate the
CAUTION
pump parts by item number and parts list. If a specific
sectional assembly drawing exists for a particular job
then that drawing should be referred to for assembly.
Refer to Table 14 for recommended torque values.
Handle inboard bearing frame bearing isolator
(169) with care. Mishandling could damage
faces of inboard bearing frame bearing isolator.
Assemble the pump in accordance with accepted rules
of engineering practice. Coat individual components with
a suitable lubricant before assembling. Assembly of unit
5. Install inboard bearing frame bearing isolator
(169) in inboard bearing frame (99).
should be performed on a clean, flat surface. During
reassembly, install parts as applicable. Assembly begins
at the suction (inboard end) of the pump.
CAUTION
While installing back-to-back ball bearings, DO
CAUTION
NOT unnecessarily hit ball bearings. If damage
to ball bearings occurs, replace damaged ball
During reassembly, install new O-rings, ball
bearings with new ball bearings.
bearings, oil seals/bearing isolators,
mechanical seals and gaskets if disturbed from
position. O-rings, ball bearings, oil
seals/bearing isolators, mechanical seals and
After 20,000 Hours of service, replace the
ball bearings.
gaskets may have been damaged during
disassembly.
6. Install new ball bearings (16) back-to-back in
bearing frame (99); back to back meaning
NOTE
lettering on the outer race facing each other.
7. Slide bearing frame (99) and ball bearings (16)
All parts should be thoroughly cleaned or
replaced with new ones if necessary. All
sealing faces should be perfectly clean, but do
not scratch or alter surface finish on seal faces.
on the coupling end of the shaft (6) up to the
bearing spacer (78).
8. The first bearing jam nut (22) is to have 3 ft-lbs
torque while holding the coupling end of the
shaft. The second bearing jam nut is to be
Parts marked with * are options that vary by
pumping unit and bearing frame size.
tightened to 30 ft-lbs while holding the first jam
nut. Install first jam nut (22) and temporarily
torque to 3 ft-lbs. Add second jam nut and
1. Confirm that the rotor TIR was completed per
Section XI, Paragraph D, step 10 before
proceeding with assembly. Secure suction
casing (9) to work area.
2. Install sleeve key (32X) into keyway in shaft (6).
Install sleeve O-ring (89X).
torque to 30 ft-lbs.
9. Temporarily secure inboard bearing cap (37) to
bearing frame (99) with washers (850), and
bolts (601).
10. Install bearing frame assembly through inboard
side of suction casing (9). Confirm proper
suction casing orientation and that wear ring
NOTE
DO NOT install mechanical seal (90*), only the
seal collar (68*).
(7A) is in suction casing.
11. Secure bearing frame (99) to suction casing (9)
by tightening bolts (600).
12. Slide spacer sleeve (14D) onto outboard end of
3. Slide sleeve (14A) onto end of shaft, lining up
keyway of sleeve with sleeve key. Install seal
collar (68*) to the scribe mark, refer to Table 6.
Secure seal collar to sleeve (14A) with sleeve
shaft (6), next to sleeve (14A).
13. Install impeller key (32A) into keyway on shaft
(6). Confirm that wear ring (7X) is in interstage
casing (111).
collar setscrews (665). Install snap ring (176) on
the shaft.
35
Page 42
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
NOTE
and interstage sleeve (58)] onto previous
interstage casing (111). Confirm interstage
Rotate pump to a vertical standing position
using a fixture that holds the suction casing
feet. This provides proper axial impeller
alignment. This eliminates sag and helps with
casing is sitting flat.
22. Repeat steps 18 through 21 for each stage up
to the Nth stage [“N” depending on the number
of stages of the pump (A,B,C,D, or E)]
figuring compression due to the tie rod
torqueing.
NOTE
Replace the same number of interstage sleeve
gaskets (73G) during assembly that were
removed during disassembly after the rotor TIR
was completed per Section XI, Paragraph D,
step 10.
IMPORTANT: Assemble shims/gaskets in the
order they were disassembled only if no
sleeves or impellers were replaced.
14. Slide first stage impeller (2A) onto shaft (6) from
outboard end, fitting keyway of impeller to
impeller key (32A) on shaft.
NOTE
Check alignment in accordance with Table 3,
Axial Impeller Alignment Control Dimensions.
15. Install interstage sleeve (58) on shaft (6) from
outboard end.
16. Lubricate and install new O-ring (89D) onto
suction casing (9). Check to make sure wear
ring and diffuser bushing (63) are in diffuser
(5A). Install new lubricated O-ring (89D) in
groove provided on interstage casing (111).
Lightly tap diffuser into interstage casing.
Confirm diffuser is sitting flat and the return
vanes are missing nub in interstage casing.
17. Install interstage casing (111) assembly [diffuser
(5A), wear ring (7X), diffuser bushing (63), wear
ring (7B), and interstage sleeve (58)] over shaft
(6) and fit onto suction casing (9). Confirm
interstage casing drain plug is oriented on the
bottom of pump and that the interstage casing
assembly is sitting flat.
18. Install impeller key (32A) into keyway on shaft
(6).
19. Install impeller (2X).
20. Check impeller (2X) alignment in accordance
with Table 3.
21. Install interstage assembly [diffuser (5A), wear
ring (7X), diffuser bushing (63), wear ring (7B),
Refer to Figure 11, the front shroud of the
impeller at the base of the wear ring surface
hits on the previous stages interstage wear ring
after the Nth stage (Refer to Table 17) and the
correct Axial Impeller Alignment cannot be
achieved ( +/- .010” ). The impeller/wear ring
interference is due to the approximately .003”
compression of each interstage casings when
tightening the tie rods.
23. When there is no impeller/wear ring clearance
there will be a gap between the impeller (2X)
and sleeve (58) (Refer to Table 17). This gap
must be measured and taken into consideration
for the Axial Impeller Alignment setting.
a. Measure the gap by leaving out sleeve (58)
and install impeller (2X).
b. Take a measurement the same way as
checking for Axial Impeller Alignment and
document.
c. Remove impeller and install sleeve.
d. Retake the measurement to see if sleeve is
holding impeller up off of the previous
interstage wear ring - this measurement
should be more than the previous
measurement and check for Axial Impeller
Alignment.
e. If measurement is not higher, then remove
impeller and add a .010” shim (73G),
reinstall impeller and retake measurement
and see if Axial Impeller Alignment
measurement increases.
f. Continue adding and counting shims until
measurement increases.
g. Repeat for remaining stages.
NOTE
Every gap that is left in the stack-up to achieve
that stage final axial impeller alignment will
compound to every stage after it and will have
to be subtracted from all final axial impeller
alignments.
36
Page 43
RS – Multi-Stage, I-280
Table 3.
Axial
Impeller
Setting
Impeller with
NO Sleeve
Measurement
Impeller
WITH Sleeve
Measurement
Number
of (.010”)
Shims to
Lift
Impeller
Axial Impeller
Alignment
Measurement
#2
Number of
Shims Left
out to
Achieve
Table 3
Setting
Gap
left in
Stack-
up
Final Axial
Impeller
Alignment
Setting
Shims to
Remove
Stage 9
Stage 10
Stage 11
Stage 12
Stage 13
Stage 14
Stage 15
Stage 16
Stage 17
Stage 18
Centrifugal Pump 280 – 16.03.EN
Example – With Standard Sleeve Bearing
– RS9-A stage 11 Axial Impeller Alignment setting = .742”
Impeller without sleeve = .760” / With sleeve = .760” – No change
Add two shims = .020” – Measurement now at .765” – meaning .015” Gap between impeller and sleeve
Remove one shim = .010” – Measurement now at .760” minus the .005” Gap and minus the .005 Gap from
stage 10 gives a Final = .750” Axial Impeller Alignment setting for stage 11 = Good due to +/- .010”
tolerance.
Example – With Optional Mechanical Seal
RS9-A stage 15 Axial Impeller Alignment setting = (-.152”)
Impeller without sleeve = (-.135”) / With sleeve = (-.135”) – No change
Add two shims = .020” – Measurement now at (-.130”) – meaning .015” Gap between impeller and sleeve
Remove one shim = .010” – Measurement now at (-.135”) minus the .005” Gap and minus the .005 Gap
from stage 14 gives me a Final = (-.145”) Axial Impeller Alignment setting for stage 15 = Good due to +/.010” tolerance.
Table 17. Axial Alignment Worksheet
37
Page 44
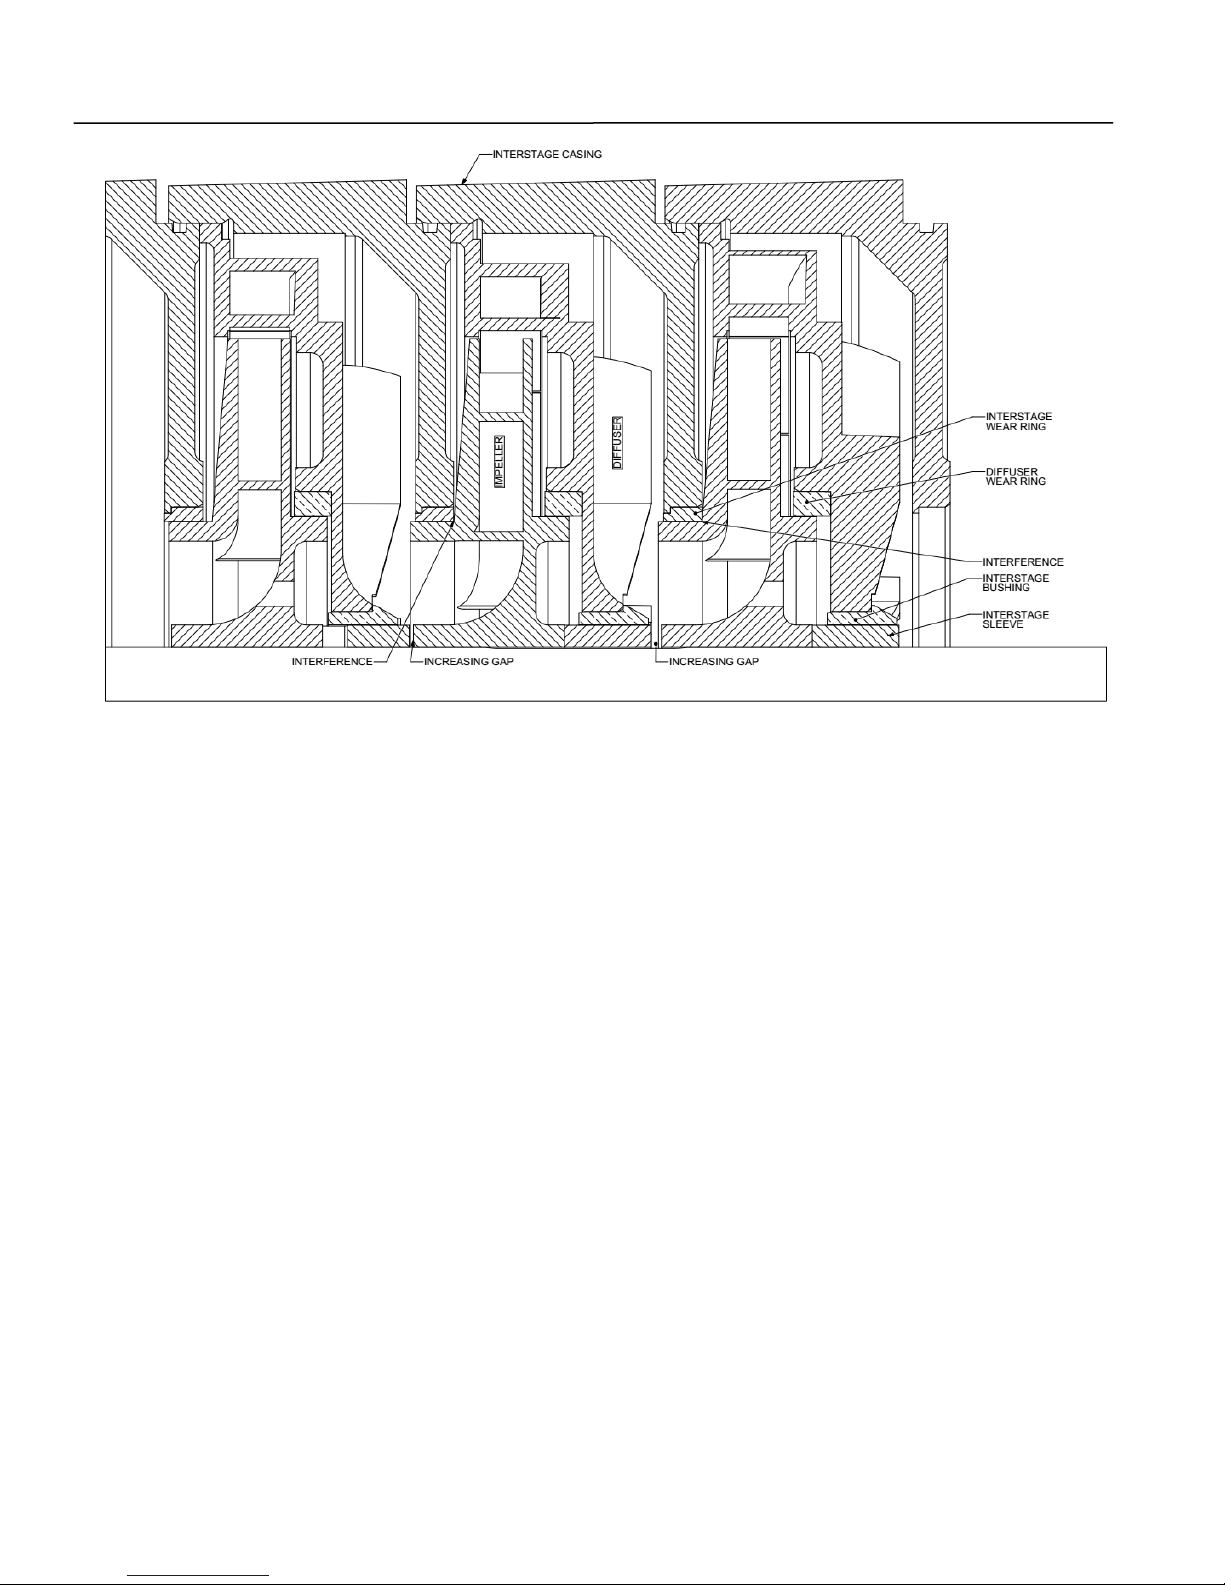
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
Figure 11. Bushing Not Torqued Interference
24. Remove interfering stages keeping close track
of how many shims are between each stage.
25. Slide outboard sleeve (14X) onto outboard end
of shaft (6), aligning keyway in sleeve with
impeller key (32).
26. Install O-ring (89A) onto last stage diffuser
bushing (63X). Install last stage diffuser bushing
into last stage diffuser (5X), make sure that
diffuser wear ring (7X) is installed in the last
stage diffuser.
NOTE
Refer to Table 5, Sleeve Bearing Dimensions to
determine if replacement of sleeve bearing
(63Y) is required.
27. Install the last stage diffuser (5X) with last stage
diffuser bushing (63X) and bushing O-ring (89A)
into the discharge case (1). Install sleeve
bearing (63Y) in discharge casing (1).
28. Install the discharge casing (1) with diffuser
(5X), and wear ring (7X) on interstage casing
(111). Confirm proper discharge casing
orientation.
29. Install tie bolts (173), washers (645) and hex
nuts (616) and torque to 50 ft/lbs temporarily.
NOTE
Remove pump from vertical position and place
in horizontal position either on a milled flat
surface or a pump base.
30. Loosen the tie bolt hex nuts (616) and tap with
soft mallet both suction and discharge casings
to make feet flat to the milled surface of the
base.
NOTE
Ensure that the pump feet are on a milled flat
surface or the base before tie rod hex nuts are
torqued.
31. Tighten hex nuts (616) firmly and evenly. Refer
to Table 14 for recommended torque
requirements.
32. Sleeve (14X) should protrude .09 inch past the
sleeve bearing (63Y), use shims to achieve gap.
33. Install shaft washer (28) on shaft (6).
38
Page 45
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
NOTE
40. Install mechanical seal (90) rotating elements
(mechanical seal spring retainer and spring).
Rotate the shaft so the mark (arrow) that was
put on during rotor TIR process is pointing
down. Tap with a soft mallet along the suction,
interstage and discharge casings. DO NOT
rotate shaft until both end jam nuts have been
torqued.
Install rubber bellow with rotating seal face by
lubricating sleeve (14A) and inside rubber
bellow of seal and push onto sleeve (14A) up to
mechanical seal spring.
41. Install gland (17A*) on suction casing (9) and
secure with gland washer (646) and gland nut
(615). As applicable, ensure tap flush lines in
34. Install one jam nut (614) and torque to 20 ft/lbs.
Use removable thread locker and install second
jam nut (614) and torque to 30 ft/lbs.
35. Install new lubricated O-ring (89H) on outboard
bearing cap (37A).
gland are positioned so flush lines (400) can be
connected.
42. Install snap ring (176), if removed in step 37,
and bearing spacer (78) with slinger (40) on
shaft (6).
36. Secure outboard bearing cap (37A) to discharge
casing (1) with nuts (615) and gland washers
(646) on studs (631).
CAUTION
NOTE
Rotate shaft (6) by hand to ensure smooth
rotation.
37. To install mechanical seal (90*), remove
temporarily installed bearing cap bolts (601),
bearing cap bolt washer (850), inboard bearing
cap (37), and bearing jam nuts (22). Remove
bearing frame bolts (600) and remove bearing
frame (99) with ball bearings (16). Only remove
snap ring (176) if snap ring is bigger than sleeve
(14A). Loosen jam nuts (614) on end of shaft (6)
to aid in snap ring removal. Torque jam nuts on
end of shaft after torqueing bearing jam nuts.
NOTE
Refer to mechanical seal vendor instructions for
complete seal installation procedure.
38. If applicable, install cartridge mechanical seal
(90*) on suction casing (9) with hex nuts (615)
on studs (630). Do not remove seal clip until
mechanical seal installation is complete. Center
drill setscrews on cartridge mechanical seal to
prevent cartridge mechanical seal sleeve from
moving during operation.
39. For type 1 mechanical seals, lubricate both
gland (17A) and stationary element (O-ring) of
mechanical seal (90) with suitable lubricant.
Insert stationary element of mechanical seal into
gland. Install O-ring (89H) on gland and
lubricate. Lubricate inside of suction casing
stuffing box.
While installing back-to-back ball bearings, DO
NOT unnecessarily hit ball bearings. If damage
to ball bearings occurs, replace damaged ball
bearings with new ball bearings.
After 20,000 Hours of service, replace the
ball bearings.
43. Install bearing frame (99) and secure with
bearing frame bolts (600). Install new ball
bearings (16) back-to-back in bearing frame
(99); back to back meaning lettering on the
outer race facing each other.
NOTE
Put removable thread locker on the second jam
nut refer to Table 14 for recommended torque
values.
44. If snap ring was removed to install mechanical
seal (90*), torque first jam nut (22) to 3 ft/lbs.,
second jam nut with removable thread locker
and torque to 30 ft/lbs. Install jam nuts (614) on
shaft (6) and torque to 30 ft/lbs.
45. Install new bearing isolator (168) in bearing cap
(37). Confirm that the breather vent (405), oil
view sight (143), and plugs (426) are still
installed in the bearing cap. Lubricate and install
O-ring (89F) on bearing frame. Secure bearing
cap to bearing frame (99) with bearing cap bolts
(601), bearing cap bolt washers (850) and
bearing cap bolt O-ring (89W).
46. Install tubing (400 and 401), as applicable.
Secure tubing by tightening nuts on male tube
39
Page 46
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
connector (410, 411 and 413) bodies, as
applicable.
47. Install plugs (421, 423, 424, 426, and 429).
48. Rotate shaft (6) by hand to ensure shaft rotates
freely. Tighten gland nuts (615) on gland (17A).
F. REASSEMBLY OF PUMP WITH OPTIONAL
MECHANICAL SEALS. Read this entire section before
reassembling the pump. The instructions that follow are
an aid for properly trained personnel to assemble your
Carver Pump. Refer to Figures 14 and 15 to locate the
pump parts by item number and parts list. If a specific
sectional assembly drawing exists for a particular job
CAUTION
then that drawing should be referred to for assembly.
Refer to Table 14 for recommended torque values.
Use a hoist with adequate lifting capacity; refer
to Section VII, Paragraph B.
Assemble the pump in accordance with accepted rules
of engineering practice. Coat individual components with
a suitable lubricant before assembling. Assembly of unit
49. Return assembly to installation site. Install pump
on base.
50. Check for soft foot, if needed correct by
should be performed on a clean, flat surface. During
reassembly, install parts as applicable. Assembly begins
at the discharge (outboard end) of the pump.
shimming or loosen and torque the tie bolts.
Soft foot will cause alignment problems and
CAUTION
may cause failure if not corrected. Secure pump
with capscrews.
51. Rotate shaft (6) by hand to insure shaft rotates
freely and no rubbing noises are present.
52. Install coupling key (46). Install coupling half on
pump shaft (6).
53. Align coupling according to Section VII,
Paragraph F.
54. Reconnect piping, gauge lines, and auxiliary
During reassembly, install new O-rings, ball
bearings, oil seals/bearing isolators,
mechanical seals and gaskets if disturbed from
position. O-rings, ball bearings, oil
seals/bearing isolators, mechanical seals and
gaskets may have been damaged during
disassembly.
NOTE
connections, as necessary. Check for smooth
shaft rotation. Check alignment again. If
different than before, you have pipe strain and
must fix the pipe to eliminate the strain.
55. Reinstall coupling guard.
All parts should be thoroughly cleaned or
replaced with new ones if necessary. All
sealing faces should be perfectly clean, but do
not scratch or alter surface finish on seal faces.
CAUTION
Pump bearing frames should be filled with
oil before starting the pumping unit. Operation
of the unit without proper lubrication can result
in overheating of the ball bearings, ball bearing
failures, pump seizures and actual breakup of
the equipment, exposing operating personnel to
injury.
56. Fill bearing frame with oil (refer to Section X,
Paragraph A and Table 12.
57. Confirm water is turned on to external flush lines
for pumps equipped with water cooling for either
the oiler or the mechanical seal.
58. Remove all tags from valves and switches.
59. Start pumping unit in accordance with Section
VIII, Paragraph C.
40
Parts marked with * are options that vary by
pumping unit and bearing frame size.
1. Confirm that the rotor TIR was completed per
Section XI, Paragraph D, step 10 before
proceeding with assembly. Secure discharge
casing (1) to work area.
2. Lubricate and install sleeve O-ring (89X) into
groove on discharge end of shaft (6).
3. Install sleeve key (32X) into keyway in shaft (6).
Lubricate inside of sleeve (14X) and slide onto
shaft, lining up keyway of sleeve with sleeve
key.
4. Install diffuser bushing O-ring (89A) on last
stage diffuser bushing (63X). Install last stage
diffuser (5X) with last stage diffuser bushing into
discharge casing (1). Confirm gland studs (630)
are installed in discharge casing.
5. Insert snap ring (176) in snap ring groove on
shaft (6). Insert shaft assembly through
discharge casing (1).
Page 47
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
6. Install bearing spacer (78) onto shaft (6).
7. Install bearing frame bearing isolator (169*) into
bearing frame (99).
17. Lubricate and install new O-ring (89D) into
interstage casing (111).
18. Install diffuser assembly [diffuser (5A), wear ring
(7X), diffuser bushing (63), and wear ring (7B)]
into interstage casing (111). Confirm diffuser
CAUTION
While installing back-to-back ball bearings, DO
NOT unnecessarily hit ball bearings. If damage
to ball bearings occurs, replace damaged ball
bearings with new ball bearings.
sits flat in interstage casing.
19. Install interstage casing (111) into discharge
casing (1).
20. Install the next stage impeller (2X) and impeller
key (32A).
21. Repeat steps 15 through 20 for each stage up
to the Nth stage [depending on the RS model
After 20,000 Hours of service, replace the
(A,B,C,D, or E)].
ball bearings.
NOTE
8. Install end of shaft (6) through outboard side of
bearing frame (99).
9. Install new thrust ball bearings (18) back-toback on shaft (6); back to back, meaning
lettering on the outer race facing each other.
10. The first bearing jam nut (22) is to have 3 ft-lbs
torque while holding the coupling end of the
shaft. The second bearing jam nut is to be
tightened to 30 ft-lbs while holding the first jam
nut.
11. Temporarily install bearing cap (37) with bolts
(601) on bearing frame (99). If removed, install
bore plug (709).
12. Install bearing frame (99) with bearing frame
bolts (600) confirm proper discharge orientation
and drain on bottom side of bearing frame.
13. Install spacer sleeve (14E*) on shaft (6).
14. Install impeller key (32A). Make sure that wear
ring (7X) is installed in diffuser (5X).
Refer to Figure 12, the back shroud of the
impeller by the wear ring surface will start to hit
on the diffuser wear ring face and diffuser
(Refer to Table 17) and Axial Impeller
Alignment cannot be achieved ( +/- .010” ).
The impeller/ wear ring interference is due to
the proximately .003” compression per
interstage casings when tightening the Tie
rods.
22. When there is no clearance between the
impeller back shroud corner by the wear ring
surface area and the diffuser, there will be a gap
between the impeller (2X) and sleeve (58)
(Refer to Table 17). This gap must be measured
and taken into consideration for the Axial
Impeller Alignment setting.
a. Measure the gap by leaving out sleeve (58)
and install impeller (2X).
b. Take a measurement the same way as
NOTE
checking for Axial Impeller Alignment and
document.
Rotate pump to a vertical standing position
using a fixture that holds the discharge casing
feet for the purpose of proper axial impeller
alignment. This eliminates sag and helps with
figuring compression due to the tie rod
torqueing.
Check alignment in accordance with Table 3,
Axial Impeller Alignment Control Dimensions.
c. Remove impeller and install sleeve.
d. Retake measurement to see if sleeve is
holding impeller up off of the diffuser - this
measurement should be more than the
previous measurement and check for Axial
Impeller Alignment.
e. If measurement is not higher, then remove
impeller and add a .010” shim (73G),
reinstall impeller and retake measurement
15. Install the last stage impeller (2X). Check the
depth reading in accordance with Table 3. If
shimming is required for proper setting use
interstage sleeve gaskets (73G), as necessary.
16. Install the next impeller key (32A) and interstage
and see if Axial Impeller Alignment
measurement increases.
f. Continue adding and counting shims until
measurement increases.
g. Repeat for next stages.
sleeve (58).
41
Page 48
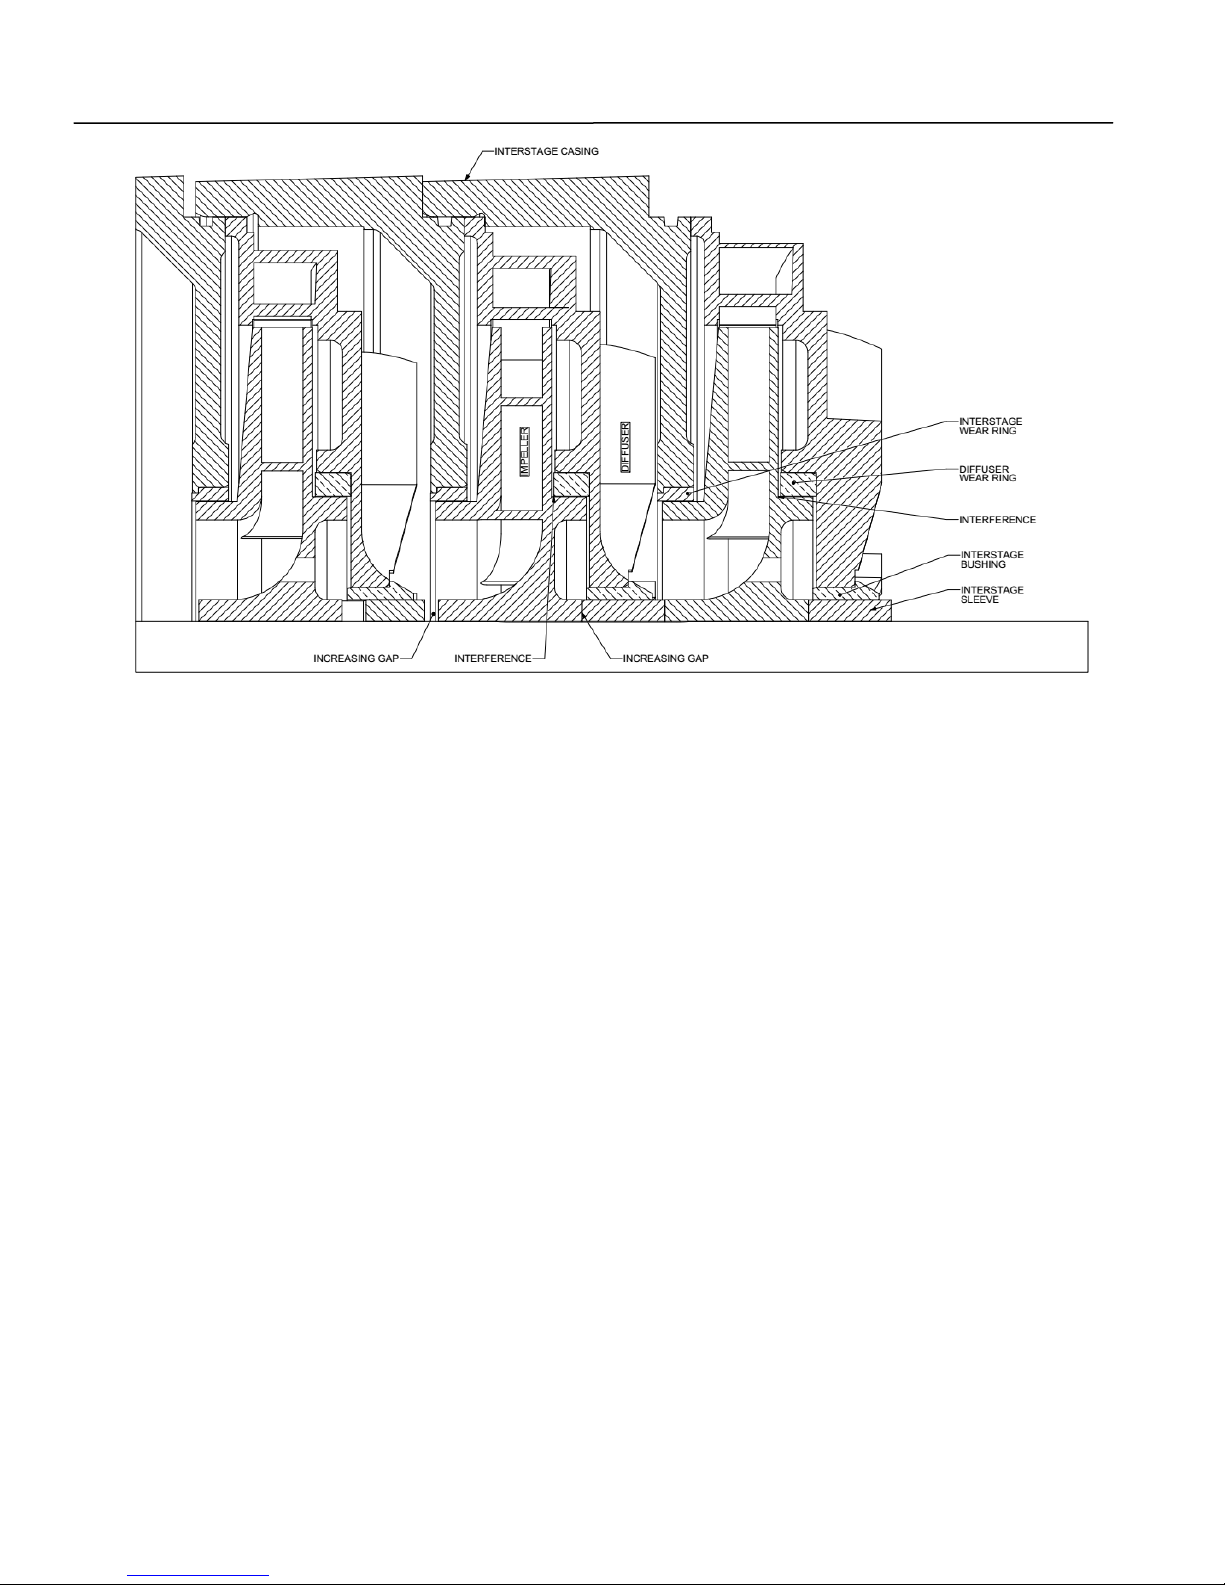
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
Figure 12. Mechanical Seal Not Torqued Interference
NOTE
Every gap that is left in the stack-up to achieve
that stage final axial impeller alignment will
compound to every stage after it and will have
to be subtracted from all final axial impeller
alignments.
23. Install spacer sleeve (14D) onto shaft (6).
24. Install key (32X) into keyway on shaft (6).
25. Mark shaft (6) and end of sleeve (14A) to
determine location of key aligning key to
keyway.
26. Lubricate and install sleeve O-ring (89X) and
slide into groove on shaft (6).
27. Install sleeve (14A) onto shaft (6).
28. Lubricate and install casing O-ring (89D) onto
suction casing (9).
29. Install suction casing (9) and tap into place
against interstage casing (111), insure proper
flange orientation of suction casing. Confirm
gland studs (630) are installed in suction casing.
30. Install tie bolts (173), flat washers (645) and tie
bolt hex nuts (616) and temporarily torque hex
nuts to 50 ft/lbs.
31. Install spacer sleeve (14G). Install bearing
frame (99) on suction casing (9) temporarily with
two bolts (600). Install bearing (16) and install
one jam nut (22), leave loose.
NOTE
Remove pump from vertical position and place
in horizontal position either on a milled flat
surface or a pump base.
32. Loosen the tie bolt hex nuts (616) and tap with
soft mallet both suction and discharge casing
feet flat to the milled surface or the base.
NOTE
Ensure that the pump feet are on a milled flat
surface or the base before tie rod hex nuts are
torqued.
33. Tighten tie bolt hex nuts (616) firmly and evenly.
Refer to Table 14 for recommended torque
requirements.
42
Page 49
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
NOTE
of mechanical seal (90*) into inboard gland.
Lubricate and install gland O-ring (89H*) on
Rotate the shaft so the mark (arrow) that was
put on during rotor TIR process is pointing
down. Tap with a soft mallet along the suction,
interstage and discharge casings. DO NOT
rotate shaft until both end jam nuts have been
torqued.
34. Torque bearing jam nut (22) to 20 ft/lbs on
suction end. Rotate pump shaft to insure shaft
spins freely.
35. To install mechanical seals, remove bearing jam
nut (22) on suction end of pump. Remove
inboard gland (17A).
43. Lubricate and Install rotating elements (rubber
bellow) of mechanical seal (90*) onto sleeve
(14A).
44. Slide inboard gland (17A*) with stationary
elements of mechanical seal (90*) over end of
shaft (6) onto suction casing (9) with studs (630)
and nuts (615) finger tight. As applicable,
ensure tap flush lines in inboard gland (17A*) is
positioned so flush lines can be connected.
45. If removed install slinger (40) on sleeve (14A).
bearing frame (99); inboard ball bearing (16),
bearing isolator (169), and spacer sleeve (78)
CAUTION
can stay in bearing frame.
Handle inboard bearing isolator (169) with care.
NOTE
Mishandling could damage faces of inboard
bearing isolator.
DO NOT rotate shaft during mechanical seal
installation. Refer to mechanical seal vendor
instructions for complete seal installation
procedure.
36. If applicable, install cartridge mechanical seal
46. Install bearing frame bearing isolator (169) in
bearing frame (99).
47. Secure bearing frame (99) to suction casing (9)
by tightening bolts (600).
(90*) on suction casing (9) with hex nuts (615)
on studs (630). Remove seal clip after pump
CAUTION
assembly is complete.
37. If applicable, for Type 1 mechanical seals
determine placement of seal collar (68*) on
sleeve (14A), refer to Table 7. For Installation of
mechanical seal (90*) rotating element, refer to
While installing radial ball bearings, do NOT
unnecessarily hit bearings. If damage to ball
bearings occurs, replace damaged ball
bearings with new ball bearings.
the following procedure:
a. Scribe a mark on the sleeve (14A) flush with
stuffing box face. Remove sleeve making
sure sleeve key (32X) stays in shaft (6)
keyway. Refer to Table 7, Standard
Mechanical Seal Settings, for specified
distance and make a second scribe mark.
After 20,000 Hours of service, replace the
ball bearings.
48. Install new radial ball bearing (16) on shaft (6).
NOTE
b. Install seal collar (68*) face to the second
scribe mark. Secure seal collar to shaft
sleeve (14A) with setscrews (665) using
Loctite to secure seal collar.
38. Lubricate inside of sleeve (14A).
Confirm the shaft, so the mark (arrow) that was
put on during rotor TIR process is still pointing
down. DO NOT rotate shaft until both end jam
nuts have been torqued.
39. Align keyway to mark scribed in step 25.
40. Slide sleeve (14A) over sleeve O-ring (89X).
41. If stationary element of mechanical seal is
replaced, clean, dry, and lubricate inboard gland
(17A*).
42. Lubricate both inboard gland (17A*), stationary
element, and O-ring of mechanical seal (90*)
with suitable lubricant. Insert stationary element
49. Install one jam nut (22) and torque to 20 ft/lbs.
Use removable thread locker and install second
jam nut and torque to 30 ft/lbs.
50. Install new bearing cap bearing isolator (168) in
bearing cap (37). Confirm that the breather vent
(405), oil view sight (143), and plugs (426) are
still installed in the bearing cap. Lubricate and
install O-ring (89F) on bearing frame. Secure
43
Page 50
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
bearing cap to bearing frame (99) with bearing
cap bolts (601). Bearing cap bolt O-ring (89W),
CAUTION
and washers (850).
51. Refer to Figure 15 for units that are oil
lube/water cooled or oil lube/air cooled for
proper installation of oil cooler (215A).
52. Use proper gasket shellac in between oil cooler
(215A) and/or gasket (73)/oil pan (215).
53. Repeat steps 34 through 50 for discharge end
of pump.
54. Rotate shaft (6) by hand to insure shaft rotates
freely and no rubbing noises are present.
Tighten gland nuts (615) on seal gland (17A*).
55. Install tubing flush lines.
56. Install plugs (424) for stuffing box, (423) for
gauge connector, and (424) for the casing drain.
Pump bearing frames should be filled with
oil before starting the pumping unit. Operation
of the unit without proper lubrication can result
in overheating of the ball bearings, ball bearing
failures, pump seizures and actual breakup of
the equipment, exposing operating personnel to
injury.
64. Fill bearing frame with oil (refer to Section X,
Paragraph A and Table 12.
65. Confirm water is turned on to external flush lines
for pumps equipped with water cooling for either
the oiler or the mechanical seal.
66. Remove all tags from valves and switches.
67. Start pumping unit in accordance with Section
CAUTION
VIII, Paragraph C.
Use a hoist with adequate lifting capacity; refer
to Section VII, Paragraph B.
57. Return assembly to installation site. Install pump
on base.
58. Check for soft foot, if needed correct by
shimming or loosen and torque the tie bolts.
Soft foot will cause alignment problems and
may cause failure if not corrected. Secure to
base with capscrews.
59. Rotate shaft (6) by hand to insure shaft rotates
freely and no rubbing noises are present.
60. Install coupling key (46). Install coupling half on
pump shaft (6).
61. Align coupling according to Section VII,
Paragraph F.
62. Reconnect piping, gauge lines, and auxiliary
connections, as necessary. Check for smooth
shaft rotation. Check alignment again. If
different than before, you have pipe strain and
must fix the pipe to eliminate the strain.
63. Reinstall coupling guard.
G. REPLACEMENT OF WEAR RING. The pump has
replaceable wear rings (7A, 7B and 7X) inserted into the
diffuser (5A or 5X), suction casing (9), and interstage
casing (111). The clearance between the wear ring and
impeller hub will increase with wear. Internal leakage will
result and pump performance will decrease. The
allowable clearance and method of measurement is
described in Section XI, Paragraph D.
NOTE
Parts marked with * are options that vary by
pumping unit and bearing frame size.
Refer to Section II for Safety precautions before
disassembling pump.
For pumps with hardened metal wear rings the
impellers need replaced if not within the
specified clearance listed in Table 18.
44
Page 51
RS – Multi-Stage, I-280
Pump Size
Casing Limits
Diffuser Limits
A
0.007 to 0.015
0.007 to 0.015
B
0.007 to 0.015
0.007 to 0.015
C
0.006 to 0.012
0.006 to 0.012
D
0.005 to 0.011
0.005 to 0.011
E
0.007 to 0.013
0.007 to 0.013
Centrifugal Pump 280 – 16.03.EN
Suction Case Wear Ring (7A).
NOTE
The suction case (9) must be removed from the base to
replace the first stage wear ring (7A). To replace the first
stage wear ring (7A) follow these steps:
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
1. Disassemble pump per Section XI, Paragraph
C, steps 1 through 15.
2. Remove suction case (9) from base and take
suction case and first stage impeller (2A) to a
work area with access to machine shop
equipment.
3. Remove the first wear ring (7A) from the suction
case (9). This can best be accomplished on a
lathe for composite wear rings. Hardened metal
wear ring can be pried out of case.
4. Press the new first wear ring (7A) into the
suction case (9). The beveled edge of the first
wear ring is installed away from the first stage
impeller (2A).
5. Place impeller (2A) on an arbor and mount
between centers in a lathe or a grinder. Indicate
front outside impeller hub to within 0.002 TIR
maximum to be sure the arbor and impeller are
running square.
6. Turn the front outside wear ring surface of the
impeller (2A) until a 63 RMS or better finish is
obtained.
7. Measure the outside diameter of the front
impeller wearing surface and record this value.
See measurement instructions in Section XI,
Paragraph D.
8. Mount the suction case (9) with new first wear
ring (7A) installed in a lathe. Indicate female
rabbet to within 0.002 TIR maximum.
When replacing first wear ring with the standard
first wear ring, (part number beginning with
"00") machining in step 9 is not required. When
replacing first wear ring with the undersize first
wear ring (part number beginning with "US")
machining in step 9 is required.
9. If replacing with an undersized wear ring, bore
wear ring (7A) to within the specified tolerance
listed in Table 18 over the recorded size of the
outside diameter of the front impeller wearing
surface.
10. Reinstall suction case (9) on base.
11. Reassemble pump. Refer to Section XI,
Paragraph F, steps 18 through 65.
Table 18. New Wear Ring
Diametrical Clearance Limits (Inches)
Diffuser Wear Ring (7X).
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
1. Complete Section XI, Paragraph C, steps 1
through 15 before continuing.
2. Remove interstage case (111) with front wear
ring (7X) still installed and the impeller (2X) to a
work area with access to machine shop
equipment.
3. Remove the front wear ring (7X) from the
interstage case (111). This can best be
accomplished on a lathe for composite wear
rings. Hardened metal wear rings can be pried
out of case.
4. Press the new front wear ring (7X) into the
interstage case (111).
45
Page 52
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
5. Place impeller (2X) on an arbor and mount
between centers in a lathe or a grinder. Indicate
front outside impeller hub to within 0.002 TIR
maximum to be sure the arbor and impeller are
running square.
6. Turn the front outside wear ring surface of the
impeller (2X) until a 63 RMS or better finish is
obtained.
7. Measure the outside diameter of the front
impeller wearing surface and record this value.
See measurement instructions in Section XI,
Paragraph D.
8. Mount the interstage case (111) with new front
wear ring (7X) installed in a lathe. Indicate
female rabbet to within 0.002 TIR maximum.
NOTE
When replacing front wear ring with the
standard front wear ring, (part number
beginning with "00") machining in step 9 is not
required. When replacing front wear ring with
the undersize front wear ring (part number
beginning with "US") machining in step 9 is
required.
9. If replacing with an undersized front wear ring,
bore wear ring (7X) to within the specified
tolerance listed in Table 18 over the recorded
size of the outside diameter of the back impeller
wearing surface.
10. Reassemble pump. Refer to Section XI,
Paragraph F, steps 18 through 65.
Interstage Case Wear Ring (7B).
When pump is handling hazardous fluid,
extreme care must be taken to ensure safety of
personnel when attempting to drain pump and
piping before disconnecting the pumping unit.
Suitable protection devices should be used
and/or protective clothing should be worn.
1. Complete Section XI, Paragraph C, steps 1
through 15 before continuing.
2. Remove interstage case (111) with back wear
ring (7X) still installed and the impeller (2X) to a
work area with access to machine shop
equipment.
3. Remove the back wear ring (7X) from the
interstage case (111). This can best be
H. MOTOR. The motor should be maintained in
I. CHECK VALVE. If applicable, the check valve
XII. PARTS LISTS AND DRAWINGS.
This section contains listings of parts and corresponding
drawings. Table 19 notes the recommended spare parts
for this pumping unit. Refer to Figures 13, 14, and 15,
for the location of parts identified by item numbers.
accomplished on a lathe for composite wear
rings. Hardened metal wear rings can be pried
out of case.
4. Press the new back wear ring (7X) into the
interstage case (111).
5. Place impeller (2X) on an arbor and mount
between centers in a lathe or a grinder. Indicate
front outside impeller hub to within 0.002 TIR
maximum to be sure the arbor and impeller are
running square.
6. Turn the back outside wear ring surface of the
impeller (2X) until a 63 RMS or better finish is
obtained.
7. Measure the outside diameter of the back
impeller wearing surface and record this value.
See measurement instructions in Section XI,
Paragraph D.
8. Mount the interstage case (111) with new back
wear ring (7X) installed in a lathe. Indicate
female rabbet to within 0.002 TIR maximum.
NOTE
When replacing back wear ring with the
standard front wear ring, (part number
beginning with "00") machining in step 9 is not
required. When replacing back wear ring with
the undersize back wear ring (part number
beginning with "US") machining in step 9 is
required.
9. If replacing with an undersized back wear ring,
bore wear ring (7X) to within the specified
tolerance listed in Table 18 over the recorded
size of the outside diameter of the back impeller
wearing surface.
10. Reassemble pump. Refer to Section XI,
Paragraph F, steps 18 through 65.
accordance with the manufacturer’s instructions.
should be maintained in accordance with the
manufacturer’s instructions.
46
Page 53
RS – Multi-Stage, I-280
Item
Number
Description
Item
Number
Description
2A
Impeller, First Stage
58
Interstage Sleeve
2X
Impeller, Per Stage
63
Bushing, Diffuser
6
Shaft
*63X
Bushing, Last Stage Diffuser
7A
Wear Ring, First Stage
*63Y
Sleeve Bearing
7B
Wear Ring, Interstage Case
69
Bearing Lockwasher
7X
Wear Ring, Diffuser
73
Gasket, Bearing Cap/Cooler
14A
Sleeve
73G
Gasket, Interstage Sleeve
14D
Spacer Sleeve, Suction and/or
Discharge End
89A
O-ring, Bushing
*14E
Spacer Sleeve, Suction and/or
Discharge End
89D
O-ring, Case
*14G
Spacer Sleeve, Suction End
*89F
O-ring, Bearing Cap
14X
Sleeve
*89H
O-ring, Bearing Gland
16
Ball Bearing, Inboard (Suction)
*89J
O-ring, Plugs/Fittings
17A
Gland, Inboard (Suction)
*89K
O-ring, Gauge Plug/Bushing
*17X
Gland, Outboard (Discharge)
*89M
O-ring, Plug
*18
Ball Bearing, Outboard (Discharge)
89W
O-ring, Bearing Cap Bolt
22
Bearing Jam Nut
89X
O-ring, Sleeve
28
Shaft Washer
89Y
O-ring, Plugs and Fittings
32A
Key, Impeller
90
Mechanical Seal, Inboard
32X
Key, Sleeve
*91
Mechanical Seal, Outboard
40
Slinger, Inboard (Suction)
168
Bearing Isolator, Inboard Bearing Cap
*40X
Slinger, Outboard (Discharge)
169
Bearing Isolator, Bearing Frame
46
Coupling Key - Pump
176
Snap Ring
*Parts are options that vary by pumping unit and bearing frame size.
Centrifugal Pump 280 – 16.03.EN
Table 19. Recommended Spare Parts List
47/(48 blank)
Page 54
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
This page intentionally left blank.
Page 55
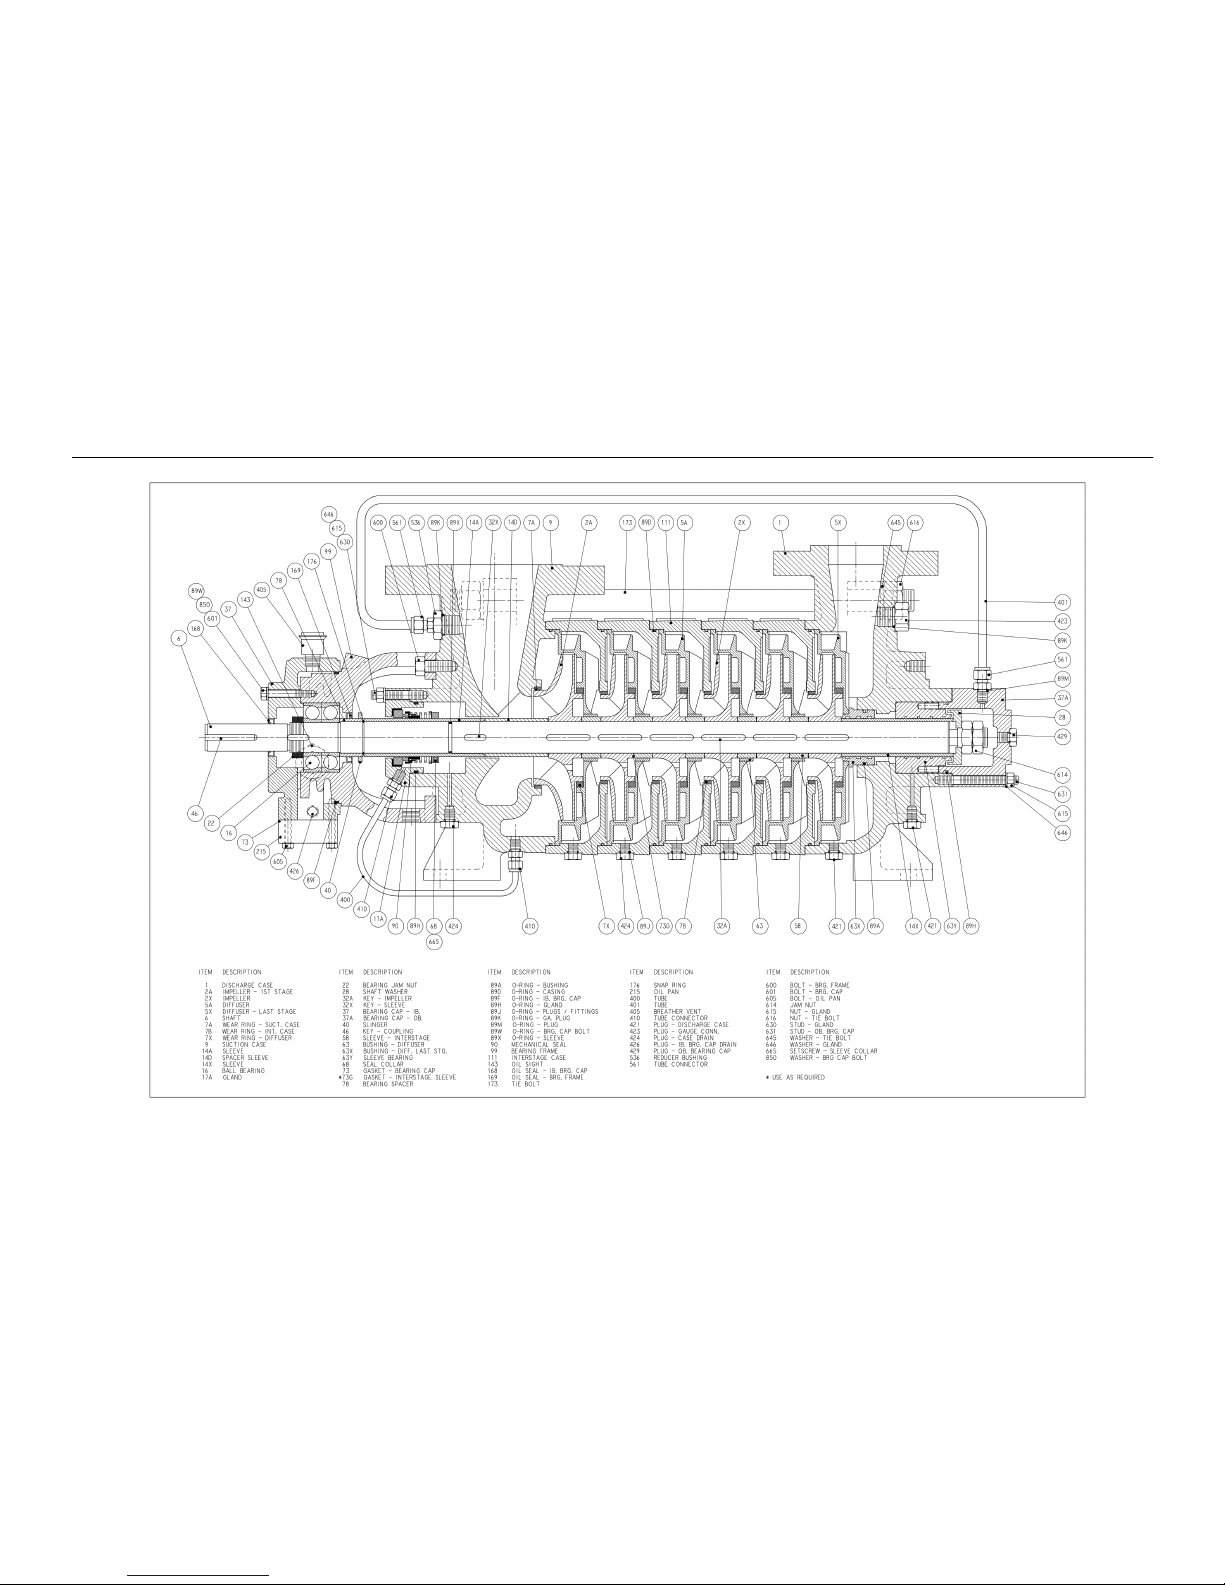
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
49/(50 blank)
Figure 13. Sectional Assembly – Standard Sleeve Bearing
NOTE
Oil lube air cooled shown. See
Figure 15 for other cooling options.
Page 56
This page intentionally left blank.
Page 57
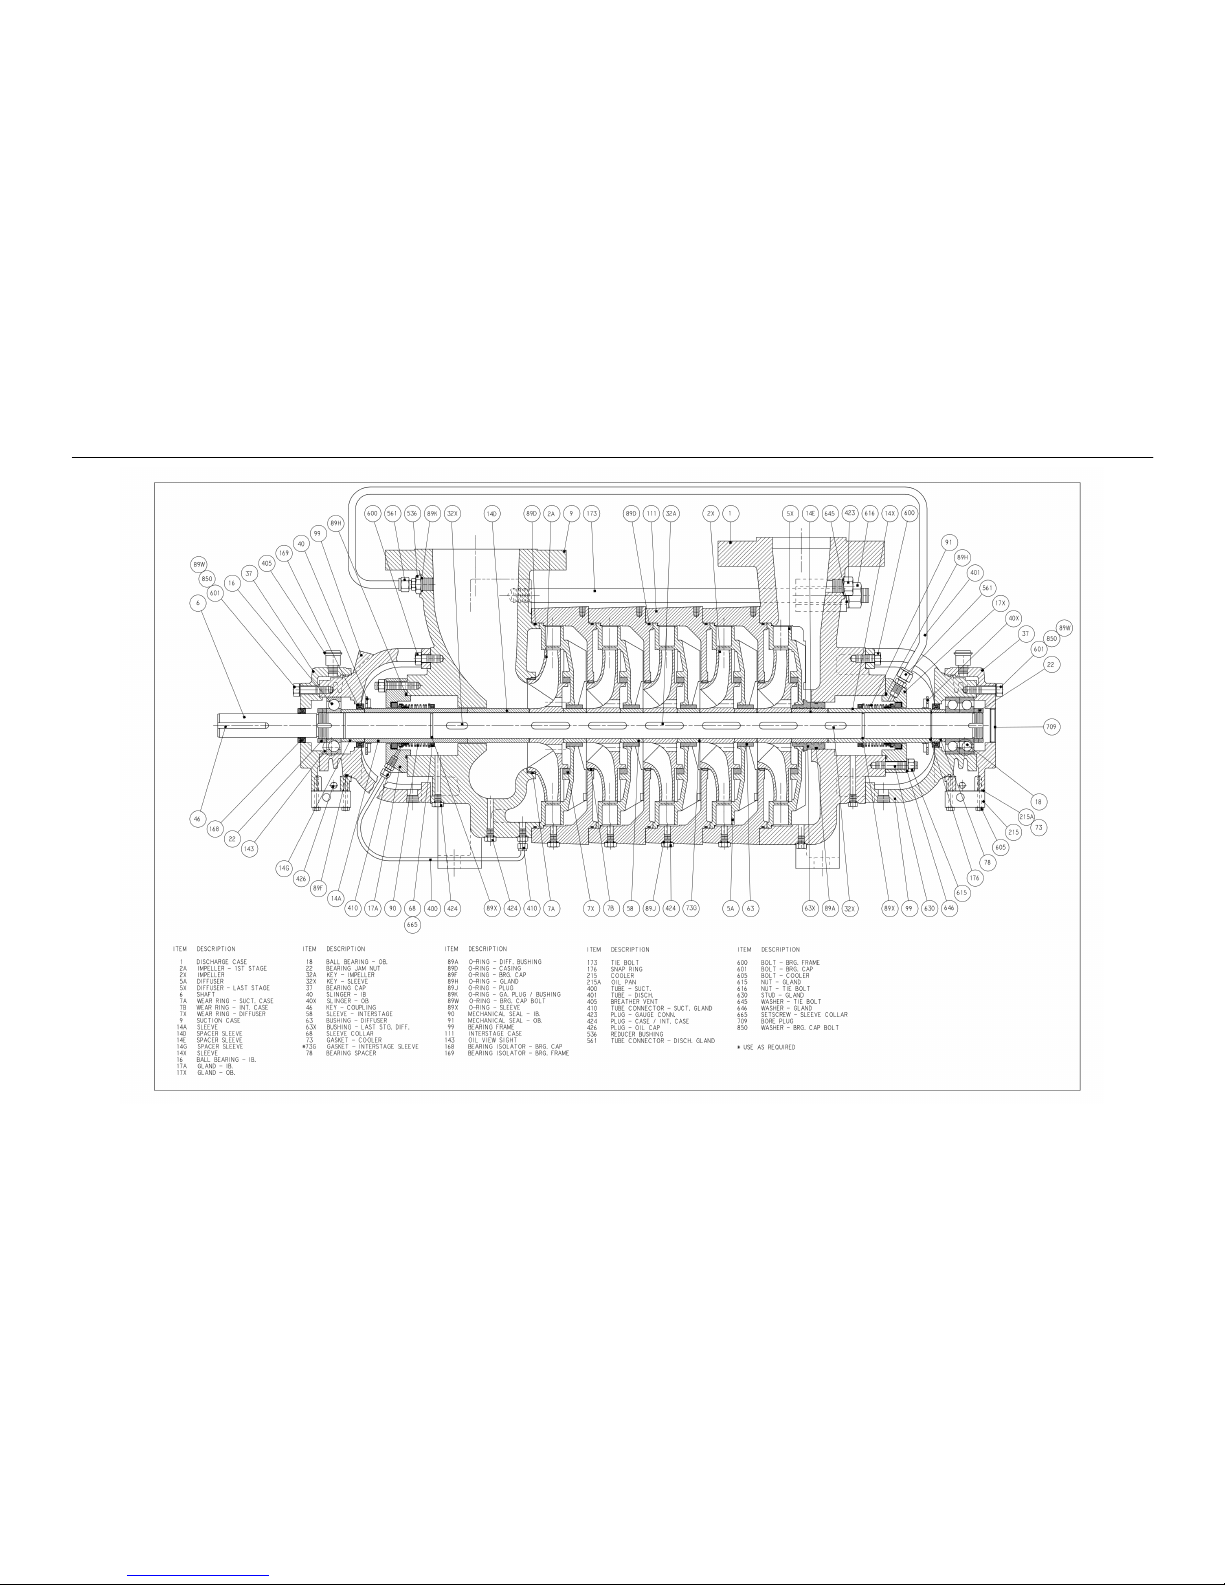
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
51/(52 blank)
Figure 14. Sectional Assembly – Optional Mechanical Seals
NOTE
Oil lube air cooled shown. See
Figure 15 for other cooling options.
Page 58
This page intentionally left blank.
Page 59
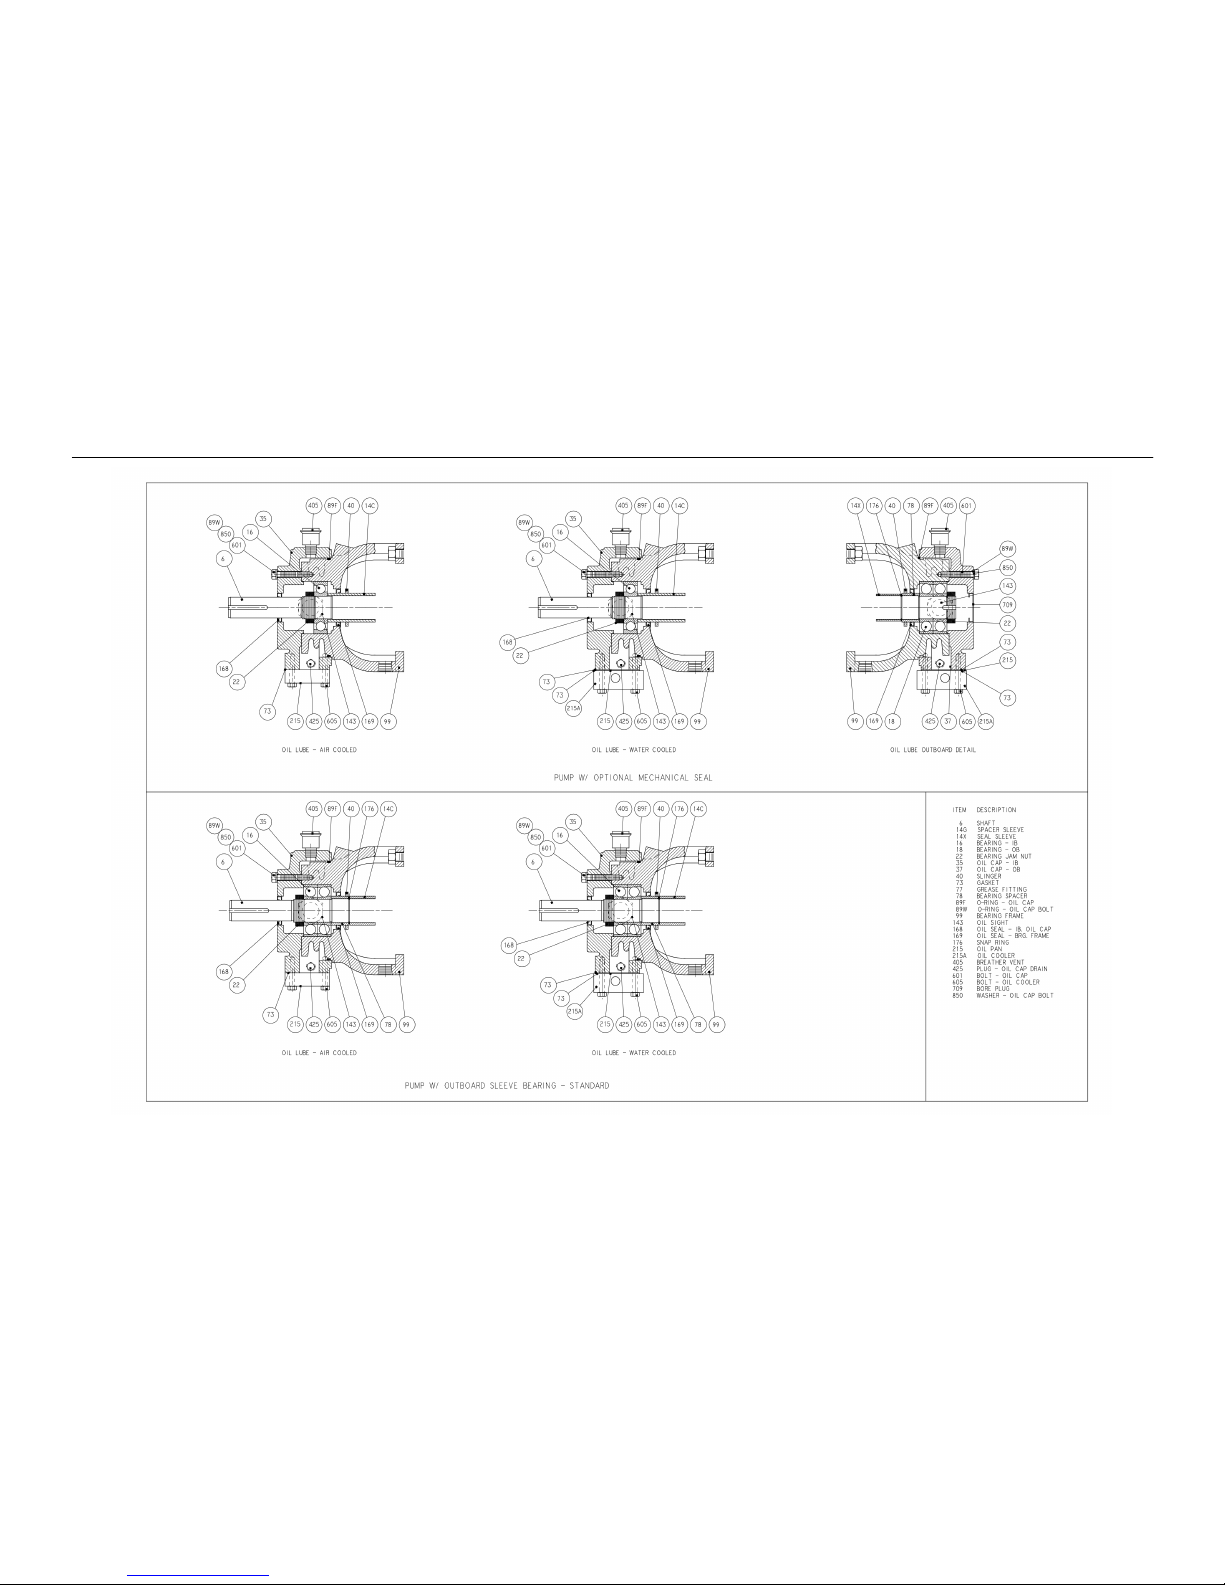
RS – Multi-Stage, I-280
Centrifugal Pump 280 – 16.03.EN
53/(54 blank)
Figure 15. Cooling Options
Page 60
This page intentionally left blank.
Page 61
This page intentionally left blank.
Page 62
RS IOM
208 – 16.03.EN
For Units Built After December 2015
2415 Park Avenue, Muscatine, IA 52761
Phone: 563.263.3410 www.carverpump.com
 Loading...