

Page 1
BURR KING MFG. CO., INC
1220 Tamara Lane
Warsaw, MO 65355
www.burrking.com
(660)438-8998 • 800-621-2748
Fax (660)438-8991
VIBRAKING 15
I
NSTRUCTION MANUAL
BURR KING VIBRAKING 15
12/2009
Page 2
BURR KING MFG. CO., INC.
1220 TAMARA LANE
WARSAW MO 65355
WWW.BURRKING.COM
(660) 438-8998 (800) 621-2748
FAX (660) 438-8991
June, 2007
Burr King Manufacturing Company. Inc. warrants the below product to be free in material and workmanship. The period of warranty is 1 year
(90 days for vibratory bowls of 20 quart and lesser volume) from the date of purchase. No warranty is provided for products that have been
modified, abused, handled carelessly, where repairs have been made or attempted by others, or for freight damage. No warranty is provided for three
phase electric motors, cont rol lers, etc. when the motors, controllers are not protected by magnetic starters that were sup plied and installed by Burr
King Manufacturing Company. Inc. No other warranty, written or verbal is authorized by Burr King Manufacturing Company, Inc.
During the warranty period Burr King Manufacturing Company, Inc (or its authorized suppliers or agents) will replace or repair the below
product without charge if the product is found by Burr King Manufacturing Company, Inc. to be defective. To receive warranty services you must
contact Burr King Manufacturing Company, Inc. and receive authorization fir warranty service. Unless otherwise author i zed by Burr King
Manufacturing Company, Inc. Products (see * below) must be returned to the factory to receive warranty service.
*Motors, speed controllers, and certain other accessories are warranted by their respecti ve manufactures. To receive warranty service on these
items you must contact a brand label service center that supports the product in need of service. Burr King Manufacturing Company; Inc. will assist
you in locating a service center.
For the first thirty days after purchase, and when Burr King Manufacturing Company, Inc. authorizes warranty service, we will pay normal and
necessary surface freight charges both ways (except for items in *). After thirty days the customer is responsible for all freight charges. Where
possible Burr King Manufacturi ng Company, Inc. may elect to make on site service and/or repairs necessary to return the product to serviceable
condition.
To assure prompt warranty service it is necessary that you complete and return the below warranty information to Burr King Manufacturing
Company, Inc. please FAX or MAIL at your convenience.
Product model: _______________________ Serial number: _______________________
Date Purchased: ______________________ Purchased from: ______________________
Address: ____________________________ City: _______________________State/Prov: _________Postal code________
Your company name: _____________________________________________
Address: _____________________________City: _______________________State/Prov: __________Postal code________
Phone: _______________________________Fax: _______________________Email: _______________________________
Your name: ___________________________Title: _______________________
How did you learn about Burr King products?
Trade show___Web___Industrial Distributor ___Advertisement ___Other __________________________Which one:________________________
What is the intended use of this product? ______________________________________________________________________________________
Please indicate the general work types performed at you r company, check all that appl y
Fabrication___Machining___Casting__Molding___Welding___Finishing___Assembly___Research___Other___
Please indicate the primary product focus of your company; check all that appl y,
Aircraft/Missile___Automotive___Contract machine___Contract Fabrication___ Agricultural____Maintenance___ Recreational___
Job shop___Foundry___Construction___Arts___Orthopedic___Dental___Medical___Other_________________________________
Please tell us what we can do to improve our products
________________________________________________________________________________________________________________________
________________________________________________________________________________________________________________________
May we contact you? Yes___No___
Thank you for purchasing Burr King products!
:
:
Register online @
www.burrking.com
Page 3
BURR KING MFG. CO., INC.
1220 TAMARA LANE
(660) 438
-
8998
s
(800) 621
-
2748
FAX (660) 438
-
8991
WARSAW MO 65355
WWW.BURRKING.COM
June 21, 2007
LETTER OF AUTHENTICITY
This letter is to certify that all Burr King Belt grinders, Disc
grinders, Polishing machines Vibra King Chambers and Bowls are
manufactured and assembled in the United States of America.
(Tariff number 847990 criterion A)
Don Mac Carthy
President
See our catalog at www.burrking.com contact us at [email protected]
Page 4
BURR KING MFG. CO., INC.
1220 TAMARA LANE
WARS A W M O 65355
WWW.BURRKING.COM
(660) 438-8998 (800) 621-2748
FAX (660) 438-8991
December 2009
Operating instructions for Model 15 VibraKING®
The VibraKING 15 vibratory bowls are stand mounted vibratory processing machines. The bowls are
compatible with ceramic, plastic, shell, cob, and most other media types. The bowls include a port for fluid
induction, and a port for fluid draining. The bowls are excellent for de-burring, de-scaling, cleaning, surface
moderating, and polishing of metals, plastics, and other materials.
Performance features of the M15
Your machine may be configured to be used with the following power. Please refer to the product label on
the machine for the power requirements.
60 hertz, 110-120 VAC, single-phase electrical power
60 hertz, 208-240 VAC, single-phase electrical power
50 hertz, 208-240 VAC, single-phase electrical power
Avoid electrocution hazards. The M15 is not NEMA 4 or NEMA 4X rated. They
must not be used in a manner that allows fluids to enter the unit base, power cord,
on/off switch, or electrical plug. This machine must be installed with a GFCI outlet to
minimize the risk of electric shock or electrocution. If your machine is configured for
208-240 volts you should install a GFCI circuit in your electrical distribution panel.
• Vibratory amplitude is easily, and continuously adjustable from zero to full amplitude.
• Standard media discharge shoot
• An integrated 0-6 hour timer
• The machine may be operated with media/ part loads from light to full capacity without damage provided
the counterweights are adjusted for the load (see next page).
• A one-half horsepower AC motor rotating within a rotation range of 1500 to 1700 RPM (dependant on
the bowl load instilled) provides vibratory energy to the bowl.
At receipt and prior to using you VibraKING
Before leaving the Burr King factory your VibraKING
that is was complete, functional, damage free, and properly packaged for shipment. You should:
• inspect the equipment for completeness and shipping damage. If anything is missing contact you’re
equipment supplier, or Burr King Manufacturing. If there is shipping damage file a claim with the freight
carrier that delivered the bowl,
• read all instructions completely. If you have questions please contact your equipment supplier or Burr
King Manufacturing for assistance,
• verify that you have your media and compound of choice,
• locate the warranty card, complete it, and return it to Burr King Manufacturing. This will insure that we
can better assist you in the unlikely event you require warranty service.
Avoid electrocution hazards. The M15 is not NEMA 4 or NEMA 4X rated.
They must not be used in a manner that allows fluids to enter the unit base, power
cord, on/off switch, or electrical plug.
Avoid fire and explosion hazards. The use of fluids other than water and
Burr King specified soaps in the bowl (or any associated fluid re-circulating system)
may create a fire/explosion hazard that could result in personal injury, or death. Use only clean water
with recommended soaps in your VibraKING
bowl
®
bowl was completely tested and inspected to assure
®
bowl and associated accessories.
®
m15 VIBRATORY opinst.doc - 9/14/2010
1
Page 5
• If you intend to use dry media such as walnut shell, or corncob the bowl ports should be left plugged.
• If you intend to use manually induced fluids, the bowl ports should remain plugged.
• If you intend to use a re-circulating fluid system (such as
the FilterPAK
4001 filtration system) connect the fluid
®
input through an appropriate metering valve to the port on
the upper rim of the bowl. Connect the drain line from the
lower port on the bowl to the drain input on the recirculating device (i.e. the FilterPAK
4001) or to your
®
fluid container. The bowl plugs are ¼ inch NP threads for
the input and ¾ inch NP threads for the drain. If you
purchased a CombiPAK
M15 you are supplied with a
®
clog resistant drain/ ½ inch hose adapter. Connect the
drain hose to this accessory.
• Fill the bowl with your media of choice. The media
should be filled to a level approximately 1 inch below the
top of the center post of the bowl.
• If you intend to use fluids, mix the fluids per the
manufacturer’s instructions and introduce the fluids into
the bowl either manually, or via your re-circulating
system. The fluid input quantity should be adjusted to
completely wet the media, but not to leave standing fluid
in the bowl.
• Instill your parts into the bowl. The maximum combined
media plus part load is:
• M15 – 150 pounds (generally 100 pounds of
media, 50 pounds of parts)
Typically, ceramic media will weight 90 to 110 pounds per cubic foot. Plastic media will weight from 40 to
60 pounds per cubic foot. Shell and cob media will weigh 20 to 40 pounds per cubic foot.
The M15 water level volume is 7.5 gallons (1 cubic feet)
• Install the bowl lid. Using the lid will dampen generated noise, and reduce fluid evaporation.
• Connect the bowl to the correct voltage for your model.
• Turn the unit ON. The media and parts should rotate in a toroid form (a doughnut shape), with the media
and parts circulating vigorously from the bowl outside toward the inner bowl post, then downward to
return to the bowl edge.
m15 VIBRATORY opinst.doc - 9/14/2010
2
Page 6
• Counter weight adjustment. If the media and part
rotation is insufficient (or to aggressive) do the
following:
• Disconnect the AC electrical power.
• Remove back panel of the base of the M15 by
using a 5/32 allen and removing the 4 bolts.
• Note the position of the two round counter
weights that are mounted on the 3/4 inch shaft .
• Loosen the setscrew on the bottom weight only.
Using a 1/8 inch allen loosen the set screw. If
the vibratory amplitude was to little rotate the
bottom weight so that it is in closer alignment
(more concentric) with the upper weight. If the
vibratory amplitude was to great rotate the
bottom weight such that it is lesser alignment
(less concentric) with the upper weight and retighten the setscrew. Maximum vibratory
amplitude occurs when the two weights are
Important! Belt tension should be approximately 1”2” of deflection at 2-3 lbs of force. Over tightening of
belt will void warranty and will cause damage to your
machine.
100% Drive or Excessive belt tension
will void factory warranty
80% Drive – Ceramic Media
exactly concentric with each other. Repeat this
process as required until you obtain a vigorous,
yet smooth toroid media and part rotation.
• General Starting Reference for different
Medias
75% Drive – Plastic Media
70% Drive – Dry Shine Media
• Reassemble the unit by reversing the
disassembly steps described above. Securely
tighten all hardware.
Removing and replacing the bowl
The bowl may be removed to empty, clean,
maintenance, or other reasons. The bowl may be
removed by simply loosening the 3/4 -16 nut and any
washers that are present.
Important! Make sure nut remains tight against
bowl washer. If nut loosens it maybe a sign of
you machine not running in the proper direction.
Adjust counterweights to proper setting and
check for bowl rotation. A nylon insert stop nut
may also be used to secure the bowl to the
machine.
m15 VIBRATORY opinst.doc - 9/14/2010
3
Page 7
Tips for optimizing your vibratory process
results
It is impossible to anticipate all possible
combinations of materials, shapes, media, and
compounds that customers may use in this
equipment. It is therefore, not possible to provide
specific directions for media selection, compounds,
process times, etc. There are, however, general
guidelines that will help to target the optimum
process. These include:
• Use the proper media to reach the result you
expect. Burr King Manufacturing will assist you in
selecting the proper media, compound, and process.
Use media that will obtain your desired finish
without lodging inside part cavities. Burr King
Manufacturing's media is available in several
grades, shapes, and material types to be best for
many part materials. Finishes can be obtained from
a light matte to a chrome like shine dependent on
part material type and incoming part finish quality.
• Clean your equipment regularly. This will
help in keeping your processed parts free of stains,
dust, etc.
• Use fresh fluids and change them often.
• Use the proper fluids (compounds) with your
media of choice. Burr King recommends BKS-60
low suds soap for non-ferrous materials, and AR-60
anti-rust soap for ferrous materials. Typically, these
soaps are mixed at 1 to 3 ounces per 1 gallon of
clean water. Note that anti-rust soaps such as AR-60
will not provide extended rust inhibition. If you
require more than a few hours of rust inhibition, you
should dip your parts in a commercially available
rust inhibitor solution.
• Clean and rinse parts quickly after processing.
Non ferrous parts may stain if not cleaned and dried
properly. Ferrous parts may
rust. There are compound
additives that will help in
removing and/or preventing
part staining.
• Media wears out in time.
The longer media is used the
less is its cutting power.
This “wearing out” is akin to
the exhaustion of life
encountered with an
abrasive belt, or wheel.
Softer materials such as
aluminum tend to clog the
media, harder materials tend
to wear the surface of the
media. The use of fluids will
help to optimize your
results. Change your media
when its size is reduced to a point that the media
lodges in part cavities, if any. Also change your
media if its shape changes to a point where it will
not reach desired surfaces.
• Burr King recommends that you establish a
regular schedule for changing and discarding your
media. You will gain knowledge regarding process
times, media life, etc.. Keeping records of your
process variables will help you optimize your
process.
• Vibratory processing creates sludge in the
liquid supply system. This sludge is a natural result
of the mechanical abrasion that occurs. The sludge
may contain abrasive residue, part material residue,
soap, or other materials that you may introduce into
the process. This sludge should be processed and
discarded in a manner that is acceptable to your
local, and/or state environmental protection
agencies. Since Burr King can not know what
materials a customer may introduce into the process,
it cannot provide specific instructions regarding this
topic. Burr King can provide MSD sheets for all
media and chemical products that it sells.
• Use a filtration system such as the Burr King
FilterPAK 4001 to keep your fluids cleaner too
greatly minimize difficulty in sludge disposal. The
FilterPAK 4001 incorporates inexpensive,
disposable filter bags that trap sludge for ready
disposal. Of course the fluid that is returned to your
vibratory chamber is much cleaner. Cleaner fluids
mean cleaner parts, better finishes, faster processing
time, and naturally less mess in your shop, and
responsible waste management. Many users who
process aluminum, steel, iron, copper, and other non
toxic metals find that the FilterPAK 4001 filter bags
may be sent to public land fills as normal refuse.
Always consult with your local authorities if you
are in doubt about
proper waste disposal.
• Maintain your media
and equipment in a clean
condition. If you use a
re-circulating, filtration
system such as the Burr
King FilterPAK
4001,
®
it will greatly reduce the
need to clean your bowl
and media. Without a
filtration system, you
will need to clean your
bowl and media at
regular intervals to
remove media sludge,
and material fines that
will accumulate inside
the bowl.
m15 VIBRATORY opinst.doc - 9/14/2010
4
Page 8
• Do not allow your parts to rest in the bowl for
extended periods. Doing so may result in stained,
oxidized, or etched parts.
• If your process uses ceramic or plastic media,
clean and dry your parts immediately after
withdrawing them from the vibratory bowl. With
dry media such as shell or cob cleaning may not be
necessary.
• Establish a process time that allows the media and
compounds of choice to process your parts to the
desired finish; control this process time from part
load to part load in order to assure consistent load to
load results.
• Pre-mix your fluids (compounds) to assure
consistent mixture. Too much soap will delay
results, too little soap will reduce finish quality, and
limit media life.
• Control the quality of the incoming part condition.
Variation in lot to lot incoming part quality may
cause variation in the vibratory process output.
Discharging media/parts
The discharge chute is located on the lower portion
of bowl. The chute plug may be removed by pulling
if free of the bowl. With the machine operating, the
media and parts (if smaller than the tube diameter)
will cascade from the tube to a container of you
choice. NOTE: When the machine approaches
empty it may begin to walk while vibrating.
Should this occur , switch main power switch to
“off” and remove the balance of the media/parts
manually.
Controlling rancid fluids
Vibratory fluids will accumulate organic
contaminants from operators, parts, etc. The fluids
may become rancid, producing a foul smell. You
can easily control rancidity by keeping your
chamber, filter system, etc. clean. In the event of
rancidity add a small amount of “Lysol” disinfectant
to the media while the machine is operating.
Ordinarily, a couple of tablespoons full will work
very well and not adversely effect your vibratory
processing. In fact, many metal react favorably with
“Lysol” by finishing to a brighter level.
Maintenance of your Burr King vibratory bowl
Maintenance consists of cleaning the unit, assuring
mechanical fasteners are secure, and assuring the
drive belt is properly tensioned.
After initial 24 Hrs of Operation
• Adjust Drive Belt Tension – ½” Deflection at 2-
3 lbs
• Inspect For Loose Hardware
Every 30 Days of Operation
• Adjust Drive Belt Tension – ½” Deflection at 2-
3 lbs
• Inspect For Loose Hardware
• Clean as Required
NOTE: Instructions for maintenance are also
printed on the maintenance label affixed to the
rear access panel of the machine.
Special note about the motor mount and drive
belt(s)
Do not over tighten the drive belt. The machine will
run better with a drive belt that in another
application would appear to be running too loose.
Over tightening the drive belt will result in
premature motor and bearing failure.
Modifications to your vibratory bowl
CAUTION: Modification of the machine from
its as shipped condition from the factory may
create a safety hazard, and may void the factory
warranty. If you have any questions in this
regard please consult the factory before making
any modifications.
Precautions you must take with fluids and other
materials
There are many different chemicals in use as
coolants, cutting fluids, and for other purposes
commonly found in facilities such as machine
shops. Burr King cannot guarantee the compatibility
of the various soaps and fluids that we sell with the
chemicals and fluids you may use. You as the
consumer must assure that the fluids and
chemicals that you elect to use are compatible
with each other and with other materials. It is
possible that chemical reactions between fluids
and/or materials that you use could be a treat to
human health and safety; and/or create
conditions that are deleterious to the VibraKING
system, peripheral equipment, and/or your parts.
There are many compounds that are available to use
in vibratory machines depending on the materials,
media, and results that you are using and desire.
Fluids and compounds serve to improve finish,
speed results, extend media life, and in some cases
m15 VIBRATORY opinst.doc - 9/14/2010
5
Page 9
to retard oxide formation. The following is a partial
list of guidelines:
1. When processing aluminum or other non-ferrous
materials to a burr free state with matte finish select
liquid soap such as BKS60 and mix it with water at
a concentration of 1 to 3 ounces per gallon of water.
Adjust the metering valve to deliver a steady trickle
of fluid to the chamber. A reasonable mechanical
gauge is to set the metering valve so that it is
approximately at a 45-degree angle to the centerline
of the valve. For finer fluid control you must install
a flow meter, most users find this unnecessary. If
you elect to install a flow meter set the fluid flow
between 1 and 8 gallons per hour as a starting point.
To improve your parts surface condition post
processing always rinse your parts in clean water
shortly after removing them from the chamber, then
dry them to minimize spotting. Remember that
many metals will oxide rapidly when machining,
etc. expose fresh metal (as is the case with vibratory
processing). If this is a problem there are various
chemicals that are available that you may use to dip
your parts in post vibratory process to minimize
oxide formation. Consult with your metals supplier,
or Burr King Manufacturing.
2. When processing steel and other ferrous materials
to a burr free state with a matte finish select a liquid
soap that also contains a rust inhibitor such as
AR60, OR RUSTX100 and mix it with water at a
concentration of 1 to 3 ounces per gallon of water.
Adjust the metering valve to deliver a steady trickle
of fluid to the bowl. A reasonable mechanical gauge
is to set the metering valve so that it is
approximately at a 45-degree angle to the centerline
of the valve. For finer fluid control you must install
a flow meter, most users find this unnecessary. If
you elect to install a flow meter set the fluid flow
between 1 and 8 gallons per hour as a starting point.
To improve your parts surface condition post
processing always rinse your parts in clean water
shortly after removing them from the chamber, then
dry them to minimize rusting. Remember that
ferrous metals will oxide rapidly when machining,
etc. expose fresh metal (as is the case with vibratory
processing). AR60, OR RUSTX100 will provide
temporary retardation of rust formation. Depending
on humidity, temperature, and other conditions the
temporary rust inhibition will be from a few hours
to several days. If your materials require longer
protection, concentrated rust inhibitors are available
that you may use to dip your parts in post vibratory
process to inhibit rust formation for several days to
several months. NOTE: RUSTX100 may be used as
a vibratory soap in concentrations up to 8 ounces
per gallon of water; used as such it provides
superior rust retardation. For special problems with
rust or other staining consult with your metals
supplier, or Burr King Manufacturing.
3. When de-scaling steel (i.e.) use a de-scaling agent
such as BKD80. This compound is used in place of
other soaps and mixed in ratios from 3 to 6
ounces/gallon of water. Following processing
neutralize the parts by dipping them in a rich
solution of AR60, OR RUSTX100 soap (6ounces/gallon water) and then dry the parts. BKD80
is corrosive, wear appropriate protective gear for
the eyes, hands, and other body tissues.
4. Many materials may be brought to a fine,
lustrous, low RMS finish by using non-abrasive
ceramic polishing media together with a burnishing
compound metered with the water. Follow the
burnishing compound manufacturer's instructions as
to concentration, etc.. Clean and dry your parts as
described above immediately after processing.
5. Many materials may be polished to a high luster
using special media such as walnut shell, corncob,
etc. Typically, these types of media are used dry,
without the use fluids. If you wish to use dry
process media do not use the liquid delivery system.
It will also be necessary to plug the outlet drain of
your VibraKING M15 to prevent the media from
escaping out the outlet. This can be done using
common plumbing devices available at ordinary
hardware stores, or from Burr King Manufacturing.
Never operate the liquid pump dry. Doing so
may damage the pump.
Accessories and supplies that are available from
your Burr King equipment supplier
• Media and compounds of many descriptions.
• FilterPAK
4001 filtration systems with
®
integrated fluid pump, filter, and fluid reservoir.
• Spare bowls, and replacement parts.
m15 VIBRATORY opinst.doc - 9/14/2010
6
Page 10
Occupational Noise Exposure
Burr King vibratory bowls produce levels of noise consistent with their intended
purposes. The level and spectral content of noise produced is dependent on the bowl
size, the degree that the bowl is maintained in proper operating condition, the
abrasive/media and accessories used, the specific application, use or not of the supplied
lid, and the surrounding environment. Noise levels produced by various Burr King
vibratory bowls, as measured at the Burr King factory, range from 76 to 88 decibels. Product
operators and persons in the immediate product vicinity should be protected from excessive noise does
levels as prescribed in OSHA regulation 29, part 1910.95 titled “Occupational Noise Exposure”.
Warranty
Burr King Manufacturing warrants the M15 against defects in material and/or workmanship for a period of
one year after original customer purchase. This warranty is in lieu of all other warranties, either expressed or
implied. Customer induced damage, miss-application, and/or abuse is not covered by warranty. To receive
warranty service you must provide the serial number of your bowl, and its original date of purchase, then
request a return authorization from Burr King Manufacturing, or an authorized distributor. All material, for
which warranty service or replacement is requested must be returned, freight prepaid to the factory for
evaluation. Burr King will (at its sole discretion) repair or replace items that qualify under this warranty. In
the event warranty coverage is extended by Burr King the warranty service will be performed without charge
(including return surface freight charges) to locations within the contiguous United States. For all other
destinations, or for other freight modes, warranty terms are FOB Warsaw, MO USA.
m15 VIBRATORY opinst.doc - 9/14/2010
7
Page 11
30
26
29
28
27
B
M15
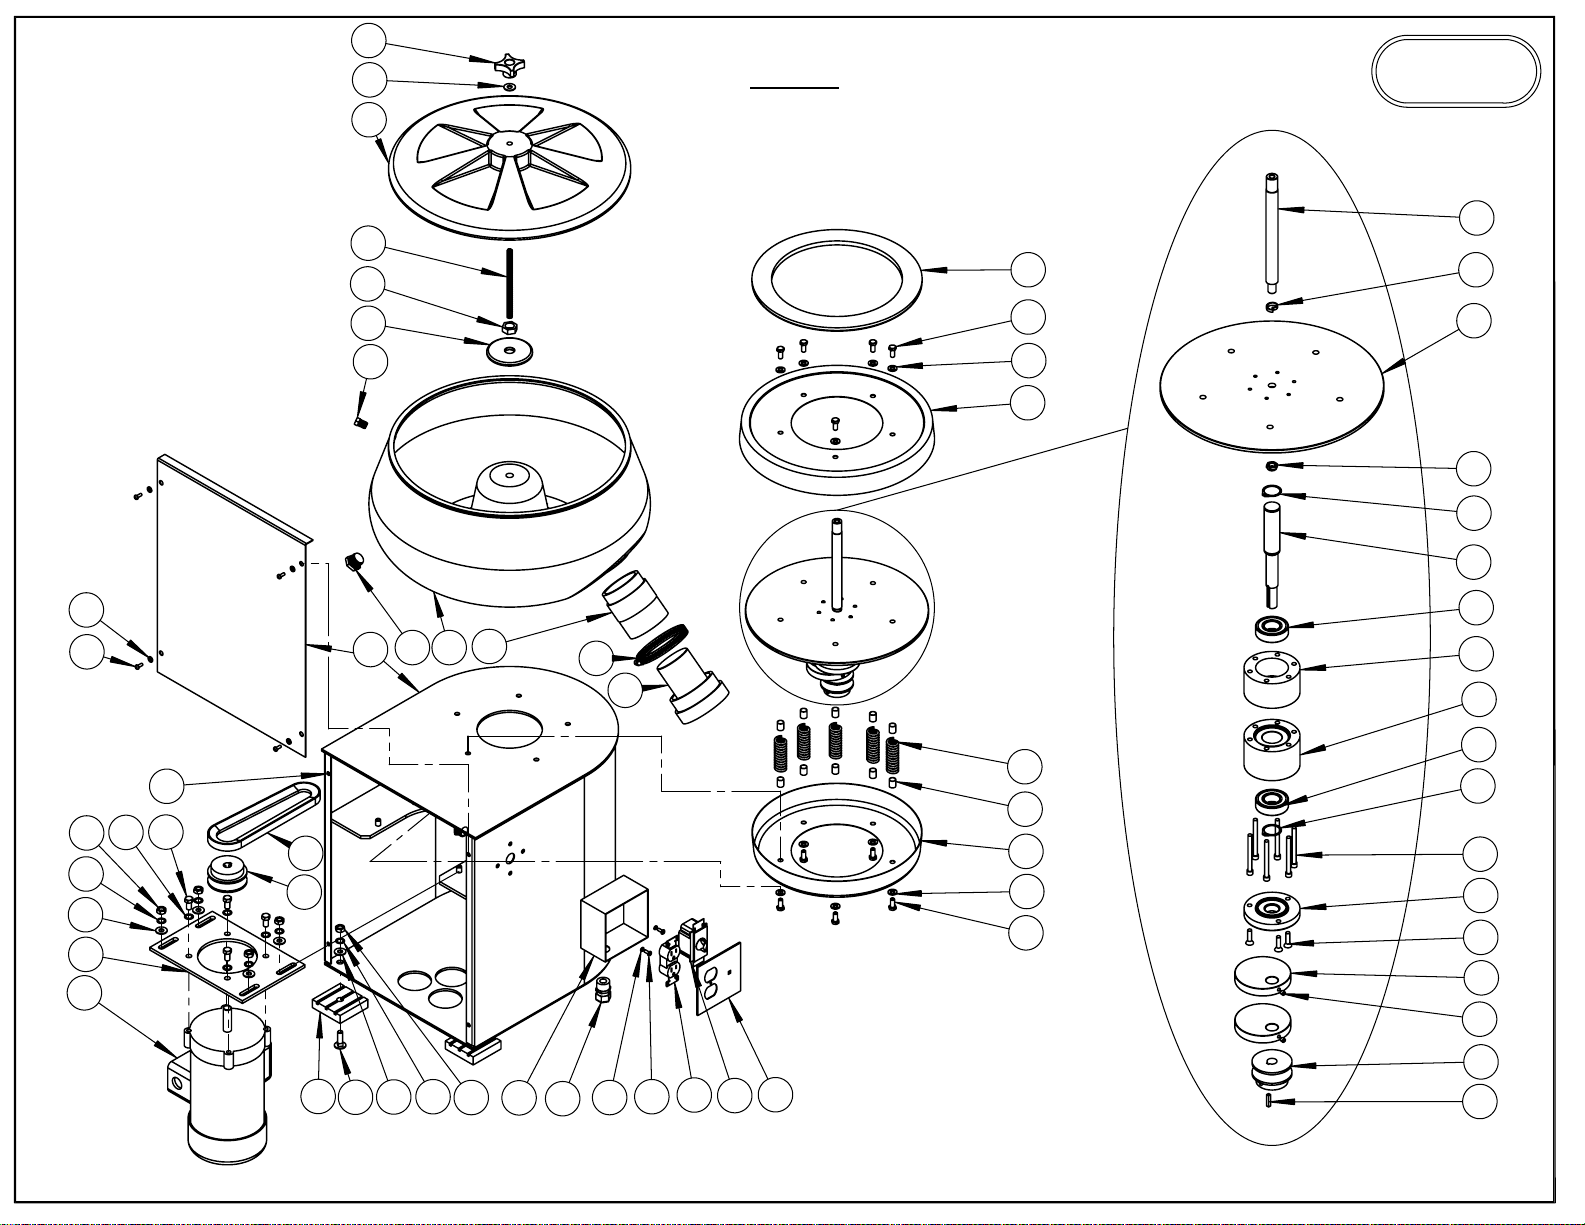
PARTS LIST
25
4
BURR KING
1220 TAMARA LANE
WARSAW, MO. 65355
9
10
8
44
45
39
40
24
5
11
13
12
14
15
16
14
7
6
3
5
4
13
17
18
19
20
21
DD
AA
26
EE
1
46
41
C
D
43
C
B
42
BB
CC
22
2
A
C
B
D
31
35
32
33
36
37
38
23
Page 12
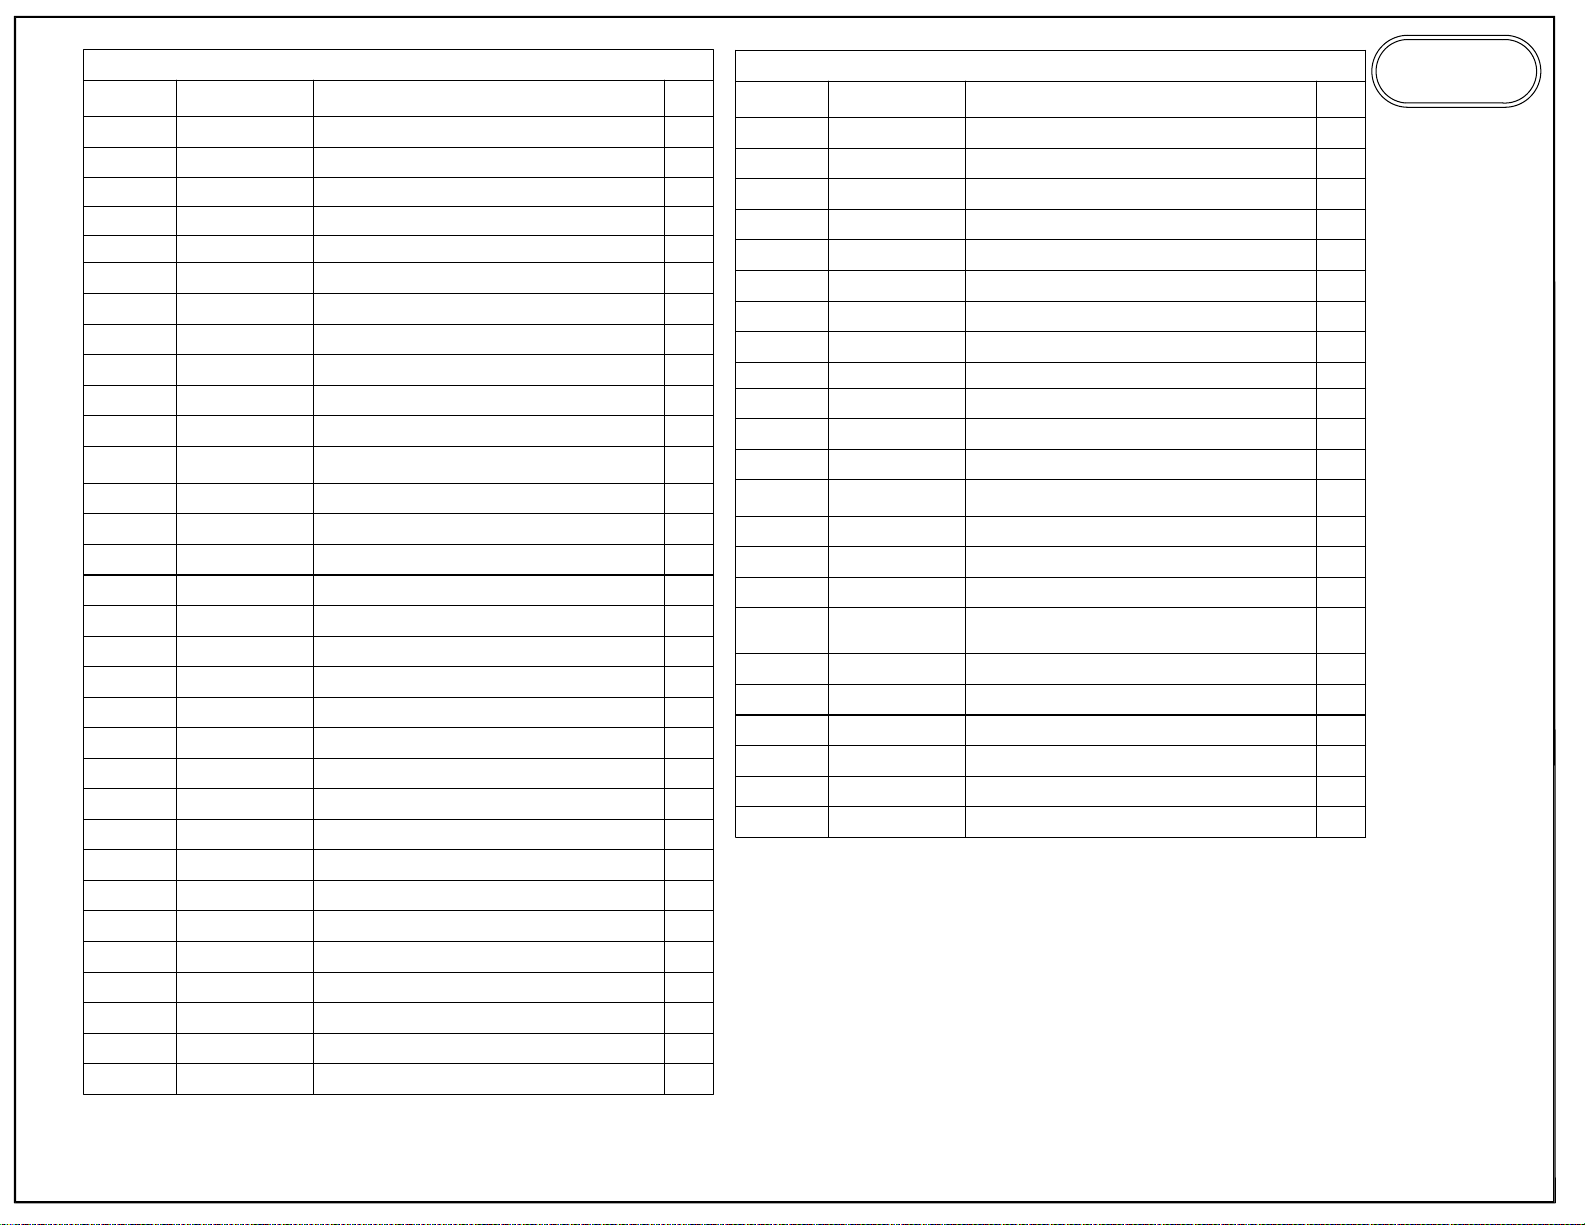
ITEM NO.
1
2 5019
A
B
C
D
3
4 37
5 4
6 5017
7 5020
8 5009
9 5012
10
11 20
12 5011
13
14
15 5008
16 5007
17
18 5016
19
20 5014
21 5021
22 5024
23
24
25 5015
26 1540
AA
BB
PART NUMBER
5000-1
1-0037
40
3B
12B
1516-3
5-0003
10-0003
11-0004
2-0058
7-0008
701G
1511-3
5006
5018
M15
DESCRIPTION
STAND ASS'Y
FEET, ASS'Y
BOLT, 3/8-16 x 1-1/4, CARRAGE
WASHER, SAE, 3/8
WASHER, LOCK 3/8, INTERNAL STAR
NUT, 3/8-16, HEX, FULL, GRD 5
COVER, SPRING
BOLT, 5/16-18x3/4 HEX, GRD5
WASHER, 5/16 SAE ZINC PLTD
SPRING, INSERT
SPRING
PLATE, BOWL
BOWL SHAFT
WASHER, 1/2 ALLEN, LOCK
NUT, NYLOK JAM, 1/2-20
SHAFT, BEARING
CIRCLIP 1" DIA
BEARING
HOUSING, UPPER BEARING
HOUSING, LOWER BEARING
BOLT, 1/4-28 x 2 3/4 SHCS
CAP, HOUSING
SCREW, 1/4-20 x 1 FHD
WEIGHT, COUNTER
SCREW, 1/4-20 x 1/4, BRASS TIP
PULLEY, 2.5 x 5/8
KEY, 3/16 X 3/16 X 7/8
SKIRT
PAD, BOWL
BOWL, ASS'Y
CHUTE
CLAMP, HOSE
QTY.
1
4
4
9
12
8
1
10
10
10
5
1
1
1
1
1
2
2
1
1
6
1
3
2
2
1
1
1
1
1
1
1
M15
ITEM NO.
CC
DD
EE
27 1030
28 1031
29
30 1500
31 3326
32 15
33 9
34 3346
35 3356
36 5004
37 5002
38 5003
39 5010
40
41
42 5023
43 5022
44 5
45 29
46 5025
PART NUMBER
1541
1506
3379
1502-1
9098-1
9098
1-0005
DESCRIPTION
PLUG, CHUTE
PLUG, PLASTIC, 1/4" MALE
PLUG, PVC, 3/4" STRAIGHT
FLANGE
NUT, RH, 3/4 x 16 HEX
SHAFT, 3/8-16-1A, 6 1/4 LONG
KNOB
BOX, 2 GANG
WASHER, #10 LOCK
SCREW, 10-24x1/2 BH
NIPPLE, CHASE 1/2"
RELIEF, STRAIN 1/2"
RECEPTACLE, DUPLEX
TIMER
PLATE, COVER, BOX
PLATE, MOTOR MOUNT
MOTOR, 1/2 HP, I PH
MOTOR, 1/2 HP, 3 PH
BOLT, 3/8-16 x 3/4, HEX
PULLY, 3.0 x 5/8
BELT, V-PULLY
WASHER, 960-416 AN
SCREW, 10-32 X 1/2 BH
CLIP, ON NUT
SEE NEXT PAGE FOR VARIABLE SPEED SET UP.
QTY.
1
1
1
1
1
1
1
1
2
2
1
1
1
1
1
1
1
4
1
1
4
4
4
BURR KING
1220 TAMARA LANE
WARSAW, MO. 65355
Page 13
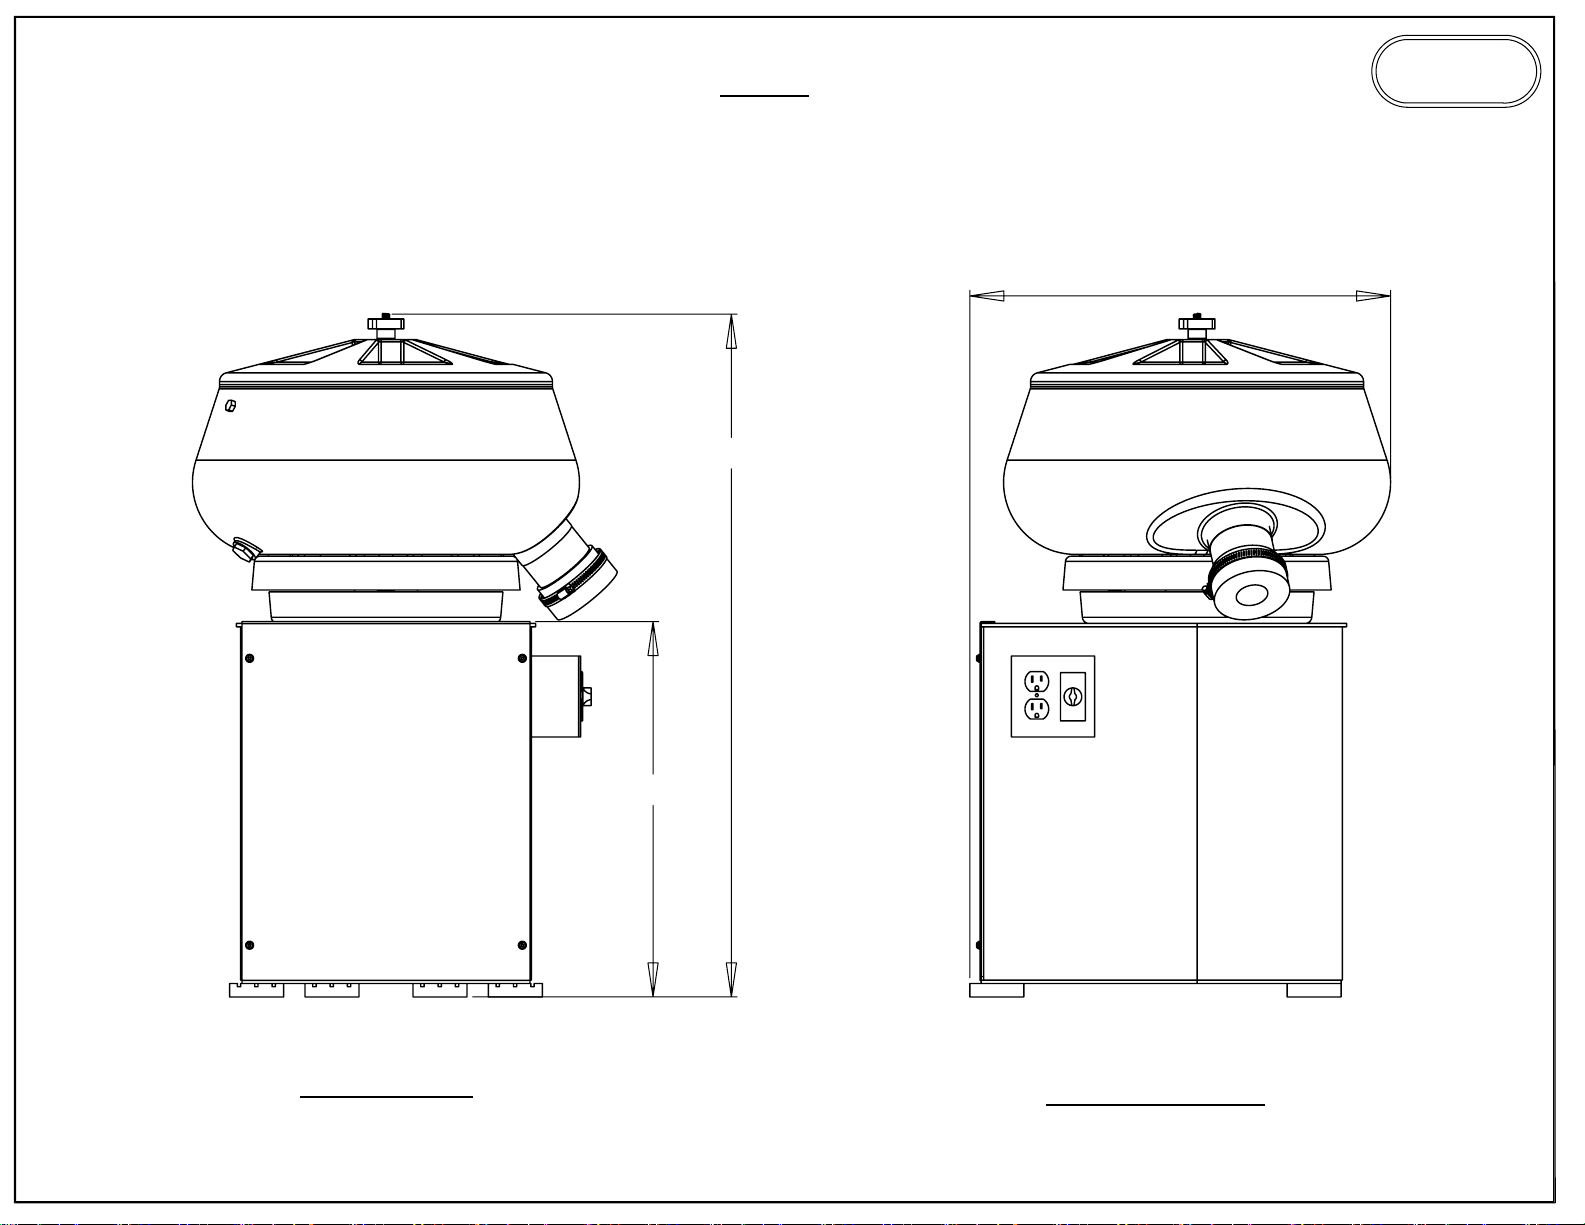
M15
LINE DRAWING
38.00
24.00
BURR KING
1220 TAMARA LANE
WARSAW, MO. 65355
BACK VIEW
20.86
LEFT SIDE VIEW
Page 14
Page 15
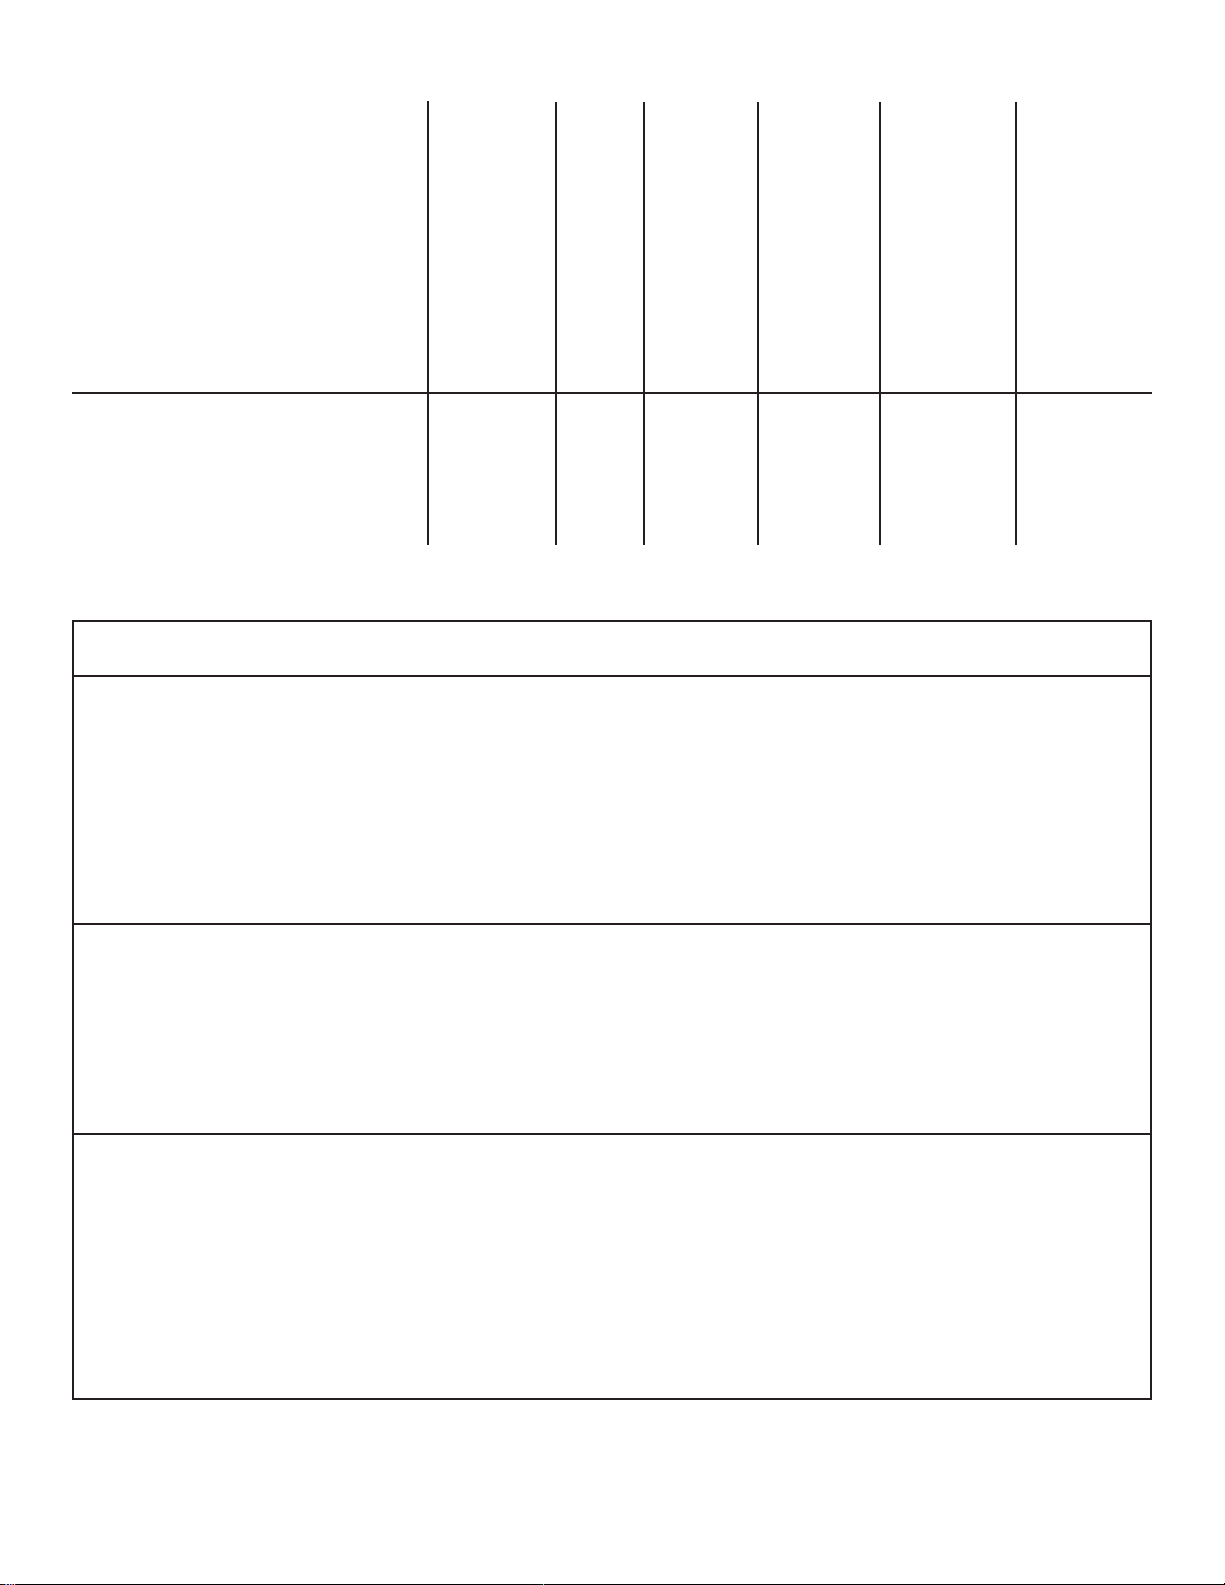
Formulations
Polish
Made of high alumina and contains no abrasives. Use with burnishing compounds to burnish
metals or with loose abrasives or
compounds for deburring. These
pins produce a high luster finish
and are suitable for use in all
types of finishing equipment.
Fast Cut
Made for fast cutting and deburring applications in all types of
finishing equipment
Formula Color Purpose Media
w
ear
Polish White Polish/
Light
deburr
Fast Cut Grey Fast Cut Good Good 100-110
Excellent Bright 115-120
Surface
Finish
CU. F.T.
Bulk Rate
Shapes/Sizes
Shapes
Diameter
Straight Cut
P
olishing
Cylinders
Diameter Diameter
Polishing
Triangle
Stock * Non Stock **
Standard Sizes
(in mm)
**
1.3 1.5
**
1.7
2.5
*
3.0
*
4.5
*
5.5
**
7.0
**
2.0
*
3.0
**
4.0
*
6.0
*
3.0
5.0
8.0
10
14
17
23
Length Length
2.0
3.0
4.0
6.0
Shapes
Fast Cut
Cylinders
Fast Cutting
Triangle
Standard Sizes
DiameterLength
2.0
2.0
2.5
3.0
4.5
2.0
3.0
3.0
4.0
6.0
(in mm)
*
**
**
*
**
**
*
*
**
**
*
Length
5.0
4.0
7.0
8.0
6.0
8.0
2.0
3.0
6.0
8.0
6.0
Diameter Diameter
Polishing
Spheres
Note: The polishing pins and polishing spheres are stocked in both OH, and CA warehouses.
Delivery on the other products listed - stock to eight weeks. Other sizes and non-standard items are
available on special order
2.0
*
3.0
*
4.0
5.0
**
6.0
*
8.0
*
10.0
**
, call for pricing and delivery. No stock 800lbs. minimum.
Fast Cutting
Spheres
2.0
3.0
4.0
5.0
6.0
9.0
10.0
**
*
**
**
**
*
**
Page 16
Burr King Mfg., Inc.
1220 Tamara Lane
Warsaw, MO 65355
(660) 438-8998 (800) 621-2748
Fax:(660) 438-8991
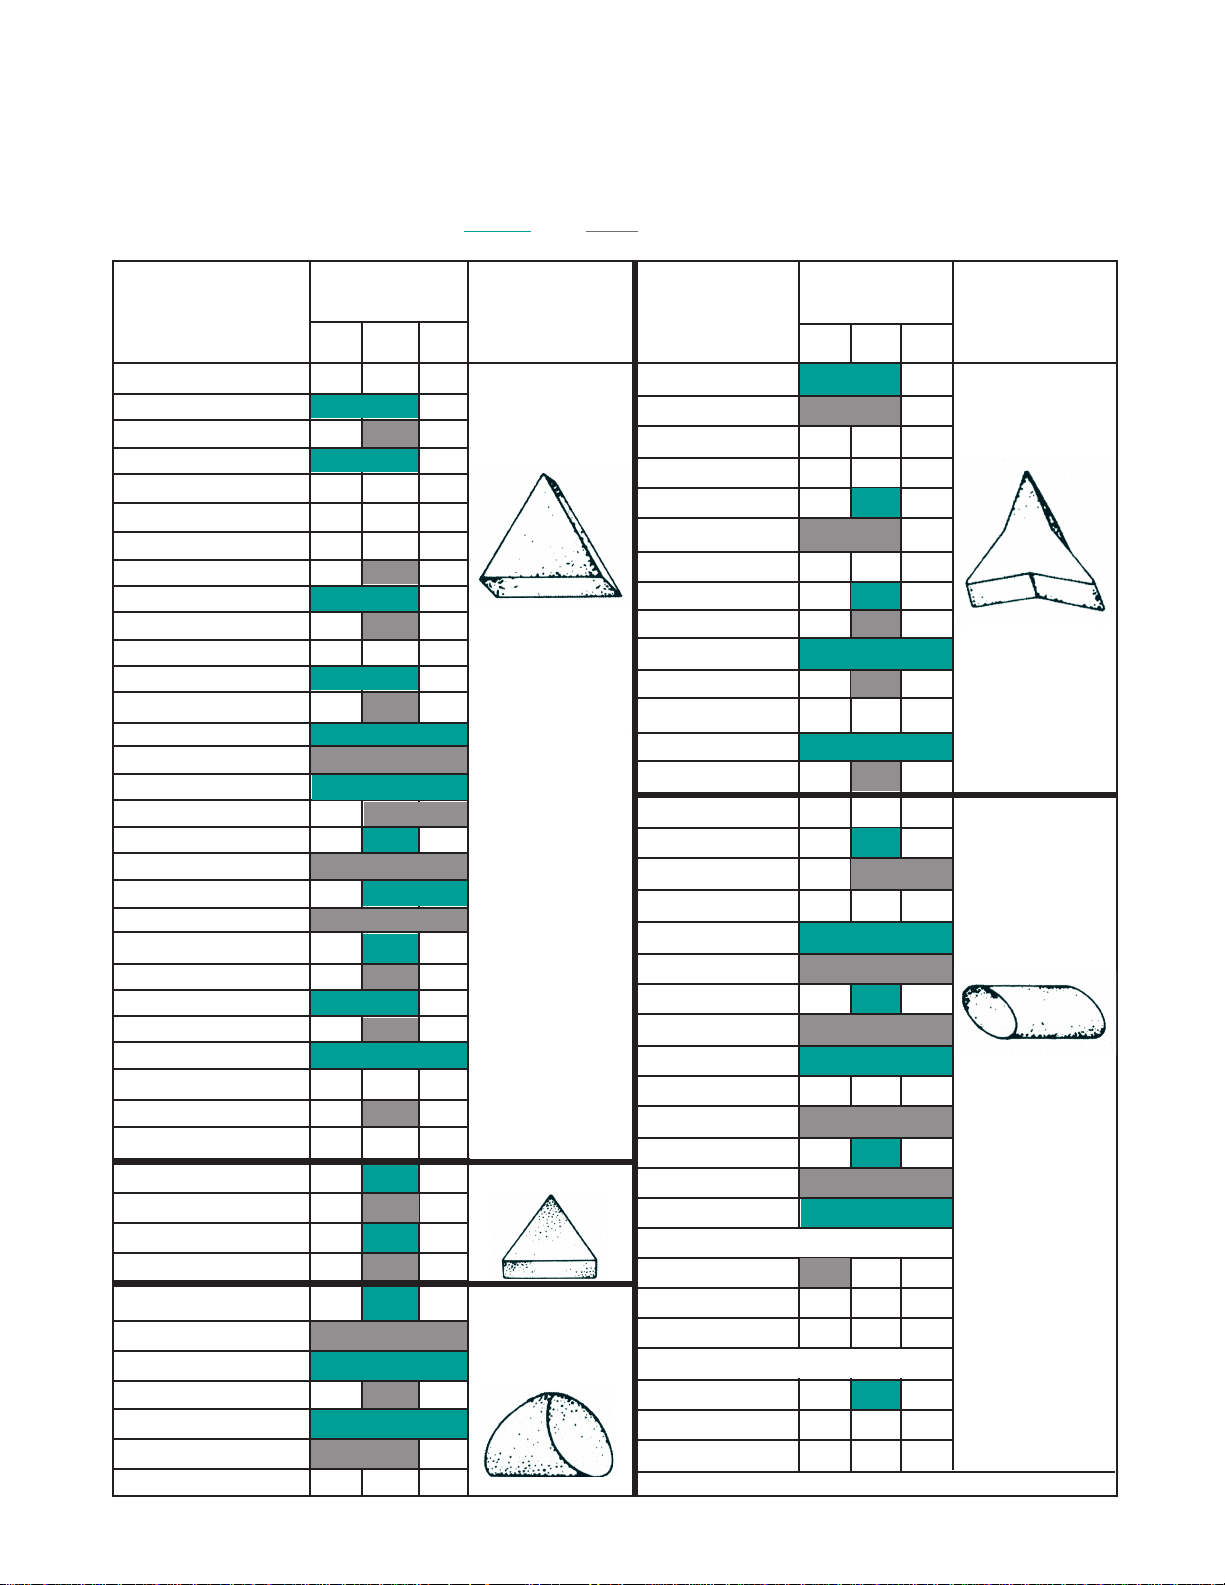
Note
: Green
Non stock items 500lb. minimum
Size Stock Shape Size Stock Shape
P-20
P-40
P-60
PREFORMED TUMBLING
AND VIBRATORY
CERAMIC ABRASIVES
and Grey fields are in stock.
P-20
P-40
P-60
2 x 7/8
2 x 11/16
1-7/8 x 7/8
1-7/8 x 5/8
1-1/2 x 1-1/2
1-1/2 x 1/2
1-3/8 x 5/8
1-3/8 x 1/2
1-3/8 x 7/16
1-1/8 x 1-1/8
1-1/8 x 1
1-1/8 x 7/8
1-1/8 x 5/8
1-1/8 x 3/8
7/8 x 7/8
7/8 x 3/8
7/8 x 5/16
3/4 x 3/4
5/8 x 5/8
5/8 x 1/2 x 5/16
5/8 x 1/4
5/8 x 3/8
3/8 x 3/8
3/8 x 1/4
3/8 x 5/16
3/8 x 3/16
1/4 x 1/4
1/4 x 5/16
1/4 x 3/16
7/8 x 1/4
7/8 x 5/8
1/4 x 3/16
1/4 x 1/4
3/8 x 3/8
7/16 x 7/16
5/8 x 5/8
3/4 x 3/4
1 x 1
1-1/2 x 1-1/2
2 x 2
le Cut
Ang
Triangle
ACT
Triangle
TRI
Cylindrical
Wedge
CW
1-7/8 x 5/8
1-3/8 x 7/16
1-3/8 x 1/2
1-1/8 x 1
1-1/8 x 7/8
1-1/8 x 3/8
1-1/8 x 5/16
7/8 x 3/8
7/8 x 7/8
7/8 x 5/16
5/8 x 3/4
5/8 x 5/16
5/8 x 1/4
3/8 x 3/16
1-1/8 x 1-3/4
7/8 x 1-3/4
7/8 x 1-1/2
3/4 x 1-1/2
5/8 x 1-1/2
5/8 x 1-1/8
1/2 x 7/8
7/16 x 7/8
3/8 x 5/8
5/16 x 5/8
1/4 x 5/8
3/16 x 5/8
3/16 x 3/8
5/32 x 5/16
ACC ELLIPSE 22 Degrees
3/8 x 5/8 x 5/8
3/8 x 5/8 x 7/8
1 x 3/8 x 1
45 & 60 Degrees
3/8 x 5/8
5/8 x 1-1/8
1/4 x 9/16
Compositions, General Info., Anti rust and soap solution on back.
Angle Cut
ristar
T
AC3S
Angle Cut
Cylinder
ACC
Page 17
Preformed Tumbling &
Vibratory Ceramic Abrasives
Compositions
P-60 = Light cut, superior finish, leaves clean surface, good for aluminum parts. (78-80lbs.)
P-40 = Good cut and wear life, excellent finish, ideal for general purpose use, economical
(89 to 90 lbs. per cubic foot)
P-20 = Fastest cut, for heavy deburring, matte finish. (85 to 90 lbs. per cubic foot)
General Information
Successful parts processing depends not only on the capability of equipment used, but also on
the type, shape and size of the media used.
Users whose work requires preforms will find that an understanding of the types available will
influence the quality of their work as well as time cycles and operating procedure.
We are totally capable of rendering assistance in your selection of specific media and equipment
for your particular problem in deburring and finishing.
We base our recommendations and technical information on testing we consider reliable, but
they are based on information we assume is correct from our dealers, agents and customers.
Soap Solutions
AR-60 -
formation. Excellent for rinse after tumbling to prevent spotting and streaking of aluminum
and magnesium. Can be mixed hot or cold. When used as a dip will impart a dry, on oily
microscopic film which does not require removal for subsequent operations. Anti rust is
mildly sudsy.
Anti Rust solution is the neutral liquid used for prevention of oxidation and rust
BKS-60 soap solution has a slightly alkaline liquid that is especially designed for vibratory
equipment as it is a low sudser. Contains some petroleum additives.
 Loading...