

Page 1
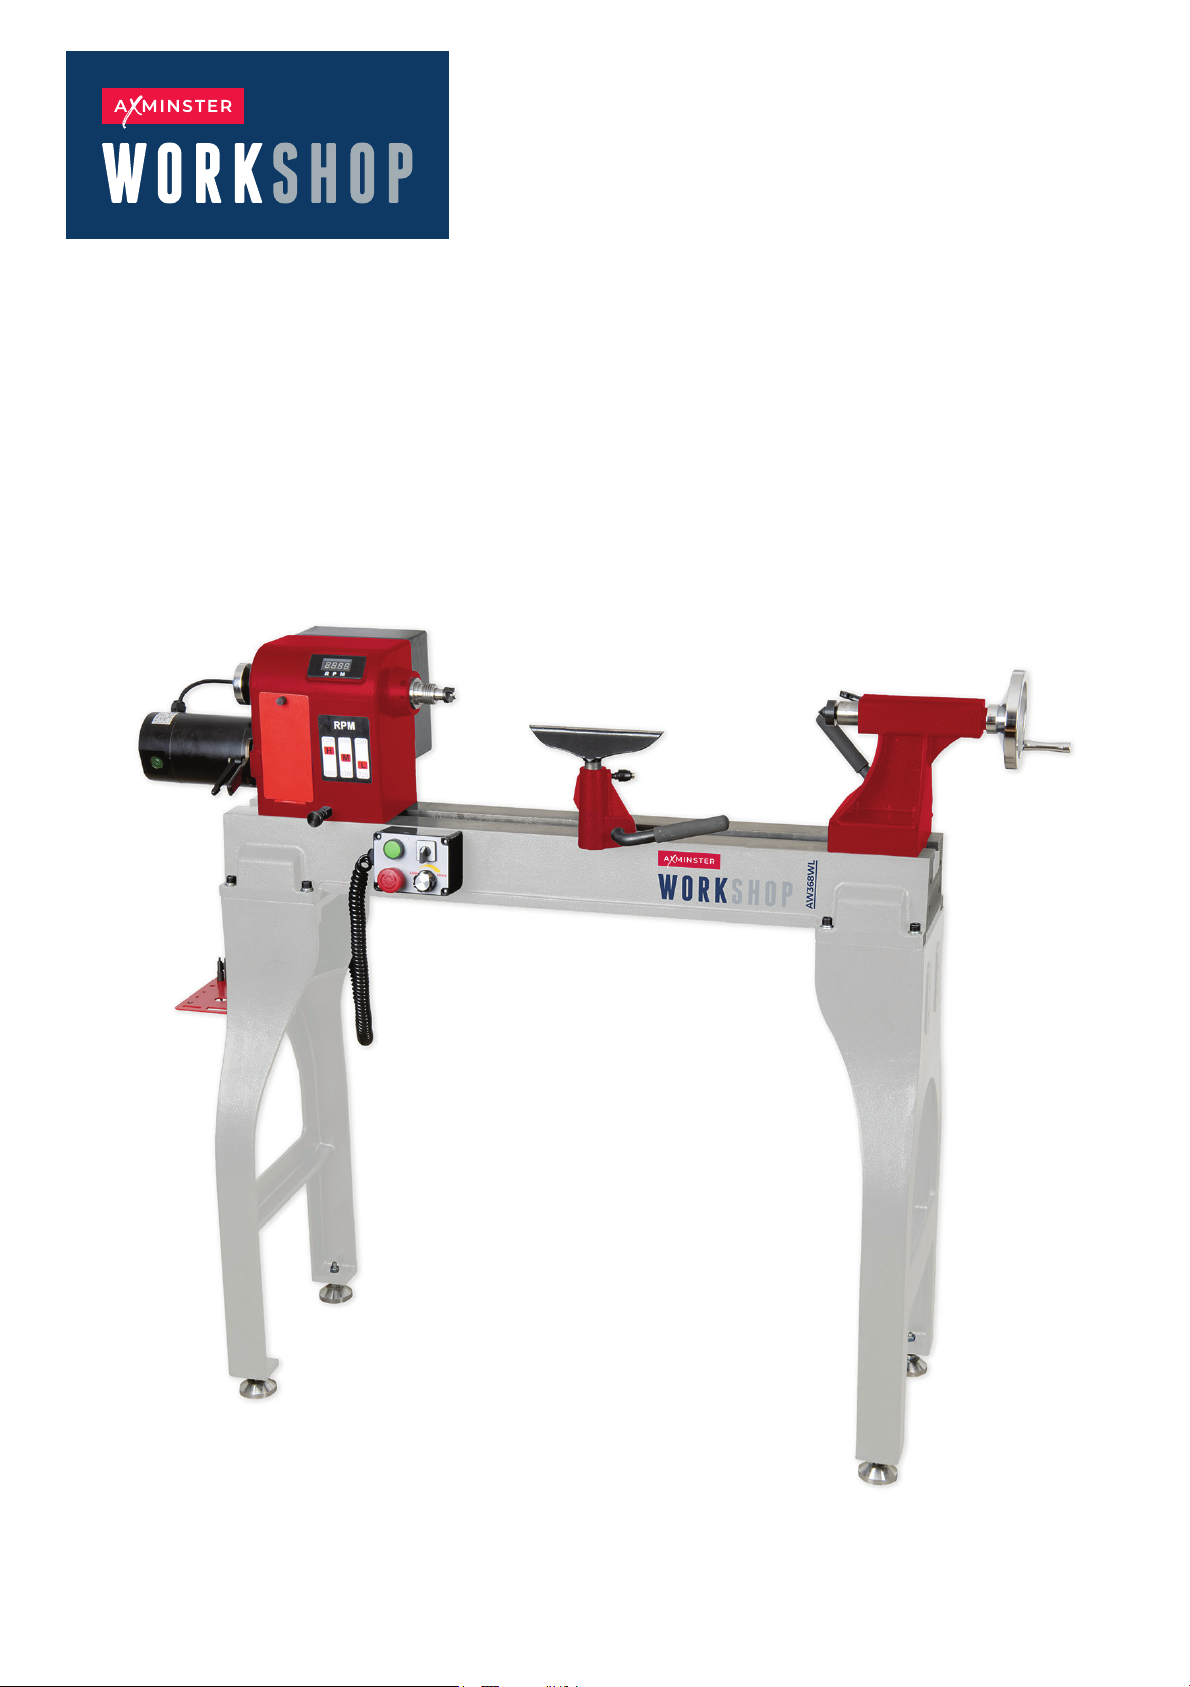
AW368WL
Woodturning Lathe
Code 107226
Original Instructions
AT: 31/07/2025
BOOK VERSION:
07
Page 2
INDEX OF CONTENTS
What’s Included 03
Optional Accessories 03
General Instructions for 230V Machines 04
Specific Safety Instructions for Wood turning Lathes 04
Specification 05
Assembly 05-06-07-08
Optional Accessories Assembly 08-09-10
Illustration & Parts Description 11-12-13
Operating Instructions
• Fitting & Removing the Faceplate 14-15
• Switch Control Box 15
• Indexing Facility 16
• Removing the Drive & Live Centres 17
• Changing the belt Speed 17-18
• Replacing the Drive Belt 18
Maintenance 19-20
Exploded Diagrams/Lists 20-21
Wiring Diagram 22
EU DECLARATION OF CONFORMITY
The symbols below advise the correct safety procedures when using this machine.
Fully read manual
and safety instructions
before use
Ear protection
should be worn
Eye protection
should be worn
2
Dust mask
should be worn
HAZARD
Page 3
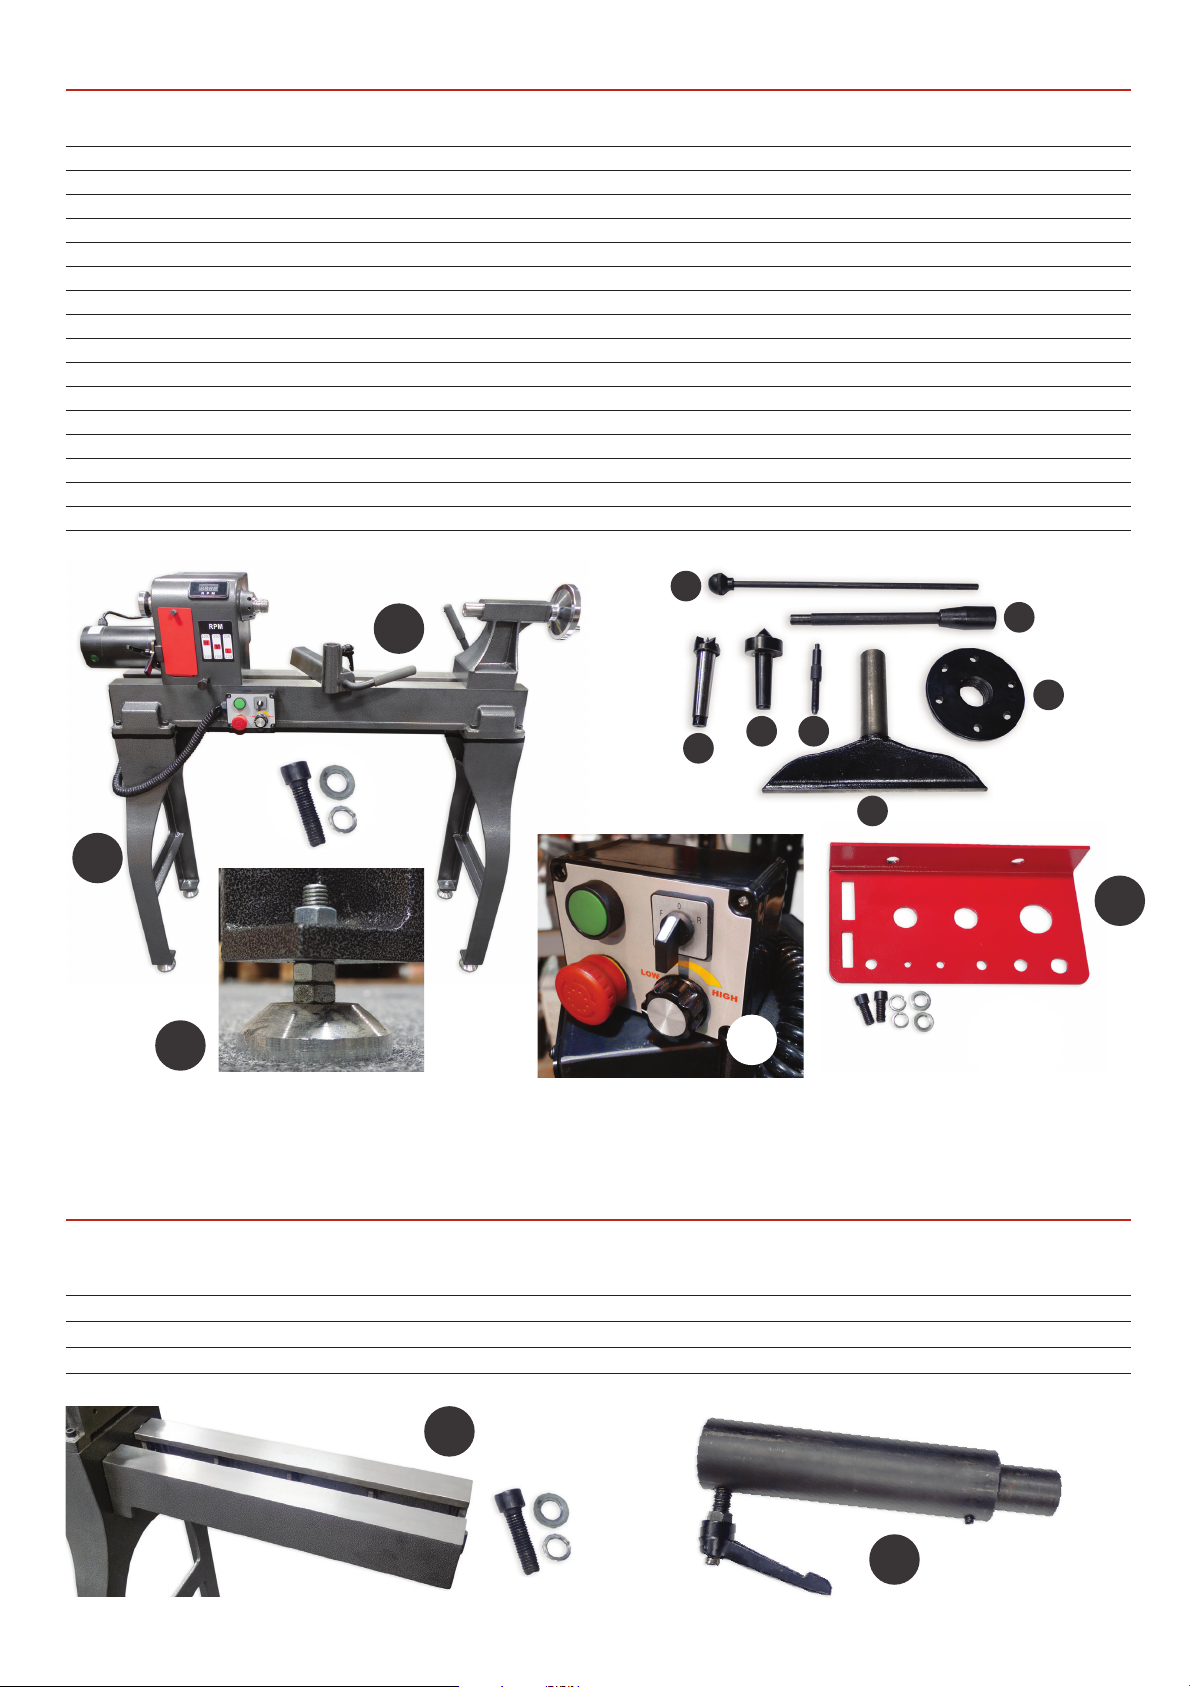
WHAT’S INCLUDED
Quantity Item Part Model Number
AW368WL
1 Woodturning Lathe A
2 Lathe Stands with Eight M10 Cap Head Bolts & Washers B
4 Lathe Stand Adjustable Feet with M10 thread & Levelling Nuts C
1 Tool Storage Angle Plate with two Cap Head Bolts,
Spring/Flat Washers
1 102mm (4 inch) Faceplate E
1 200mm Tool Rest F
1 2MT Four Prong Drive (Headstock) G
1 2MT Live Centre (Tailstock) H
1 Index Pin with M8 Thread I
1 Headstock Locking Bar/Handle J
1 Push Rod K
1 Switch Control Box L
1 230V Power Lead
1 Instruction Manual
K
J
A
I
G
H
F
B
C
Supplied with four prong Axminster drive centre code 340106 and Axminster revolving tailstock centre code 340203
Quantity Item Part
L
OPTIONAL ACCESSORIES
E
D
1 Lathe Bed Extension
with four M10 Cap head Bolts & Washers M
1 Banjo Tool Rest Extension Post N
M
3
N
Page 4
GENERAL INSTRUCTIONS FOR 230V MACHINES
The following will enable you to observe good working
practices, keep yourself and fellow workers safe and
maintain your tools and equipment in good working
order.
WARNING!! KEEP TOOLS AND EQUIPMENT OUT
OF REACH OF YOUNG CHILDREN
KEEP WORK AREA AS UNCLUTTERED
AS IS PRACTICAL. UNDER NO CIRCUMSTANCES
SHOULD CHILDREN BE ALLOWED IN WORK
AREAS.
Mains Powered Tools
• Tools are supplied with an attached 13 Amp plug.
• Inspect the cable and plug to ensure that neither
are damaged. Repair if necessary by a suitably qualified
person.
• Do not use when or where it is liable to get wet.
Workplace
• Do not use 230V a.c. powered tools anywhere
within a site area that is flooded.
• Keep machine clean.
• Leave machine unplugged until work is about to
commence.
• Always disconnect by pulling on the plug body and
not the cable.
• Carry out a final check e.g. check the cutting tool
is securely tightened in the machine and the correct
speed and function set.
• Ensure you are comfortable before you start work,
balanced, not reaching etc.
• Wear appropriate safety clothing, goggles, gloves,
masks etc. Wear ear defenders at all times.
• If you have long hair wear a hair net or helmet to
prevent it being caught up in the rotating parts of the
machine.
• Consideration should be given to the removal of rings
and wrist watches.
• Consideration should also be given to non-slip footwear
etc.
• If another person is to use the machine, ensure they are
suitably qualified to use it.
• Do not use the machine if you are tired or distracted
• Do not use this machine within the designated safety
areas of flammable liquid stores or in areas where there
may be volatile gases.
• Check cutters are correct type and size, are undamaged
and are kept clean and sharp, this will maintain their
operating performance and lessen the loading on the
machine.
• OBSERVE…. make sure you know what is happening
around you and USE YOUR COMMON SENSE.
SPECIFIC SAFETY INSTRUCTIONS FOR WOOD TURNING LATHES
1. Do not use ‘split’ work pieces.
2. Always start at the lowest speed when starting a new
task.
3. Check that the tool rest is at or slightly below the
centre line of the work piece.
4. Check the work piece is securely mounted in the
lathe before switching on the power.
5. Rotate the work piece by hand, to check that it is
centralised, clear of the tool rest, not ‘split’ or has loose
knots.
6. Where lathes have the facility to be reversed; check
the machine is rotating in the correct direction.
7. If your lathe has the facility to run in reverse, you
must ensure that the mounting accessories (chucks,
faceplates etc.,) can be ‘locked’ onto the lathe mandrel,
and in the case of chucks, have some form of security
device to prevent them ‘unwinding’ during reverse
operation.
8. Make sure your tools are stored/racked away from the
turning area of the lathe. Do not reach over a rotating
work piece at any time.
9. Do not ‘dig in’ or try to take to large a cut.
10. Do not leave the lathe running unattended; or leave
the machine until everything has stopped.
11. Some turning tools may have specific sharpening
angles that have been determined by the manufacturers; when re-sharpening, adhere to these angles to
maximise the finish of your work.
4
Page 5
SPECIFICATION
Model AW368WL
Rating Home Workshop
Power 750 W
Spindle Thread M33 x 3.5 mm
Spindle Speed (L) 250-720 rpm, (M) 550-1,700 rpm, (H) 1,200-3,350 rpm
Forward/Reversing Function YES
Swivel Headstock 60˚, 90˚, 120˚, 180˚ (degrees)
Headstock Taper 2 MT
Tailstock Taper 2 MT
Faceplate Diameter 102mm
Distance Between Centres 610 mm
Distance Between Centres with Extension Bed 1120 mm
Indexing Positions 36
Max Diameter over Bed 368 mm
Max Diameter over Tool Rest 280mm
Tool Rest Stem Diameter 25.4 mm (1”)
Tool Rest Width 200 mm
Overall L x W x H 1,400 mm x 400 mm x 1,250 mm
Weight 137 kg
Important Notes
Please take some time to read the section entitled
‘Illustration and Description’ to identify the various
parts of your machine so that you are familiar with the
terminology we will use to enable you to set up and
operate your table lathe safely and correctly.
The lathe and its accessories will arrive coated with
corrosion preventative grease. This will need to be
cleaned from the lathe, its components and accessories prior to it being set up. Wearing overalls and rubber
gloves is advisable, as is eye protection. After cleaning,
lightly coat the machine with a thin layer of light wax.
UNPACK YOUR NEW LATHE AND RECYCLE THE
PACKAGING RESPONSIBLY. THE CARDBOARD
PACKAGING IS BIODEGRADABLE.
ASSEMBLY
PLEASE NOTE: The Lathe comes 90% pre-assembled.
In order to reduce the footprint of the machine for
packaging, several items are dismounted from the
machine and need to be re-affixed. Please check all the
boxes, packets etc. to make sure that all the parts have
been accounted for.
1. Remove the headstock and tailstock stop pins to the
ends of the lathe bed and place safely aside.
2. Carefully remove the headstock, tailstock and tool rest
banjo and place safely aside.
NOTE: When removing the headstock assembly, make
sure that the control box power cord is well clear of any
sharp objects.
3. Using a lifting device or seek help, lift the lathe bed
from the pallet onto a work bench in readiness to mount
the leg stands (B).
WARNING: THE WOOD LATHE IS A HEAVY
MACHINE, IT IS ADVISABLE TO USE A LIFTING
DEVICE SUCH AS A HOIST, SCISSOR LIFT OR SEEK
HELP WHEN ASSEMBLING THE LATHE.
WARNING! WE RECOMMEND YOU REMOVE THE
HEADSTOCK, TOOL REST AND TAILSTOCK FROM
THE LATHE BED BEFORE LIFTING THE LATHE
ASSEMBLY OFF THE PALLET
Stand Assembly
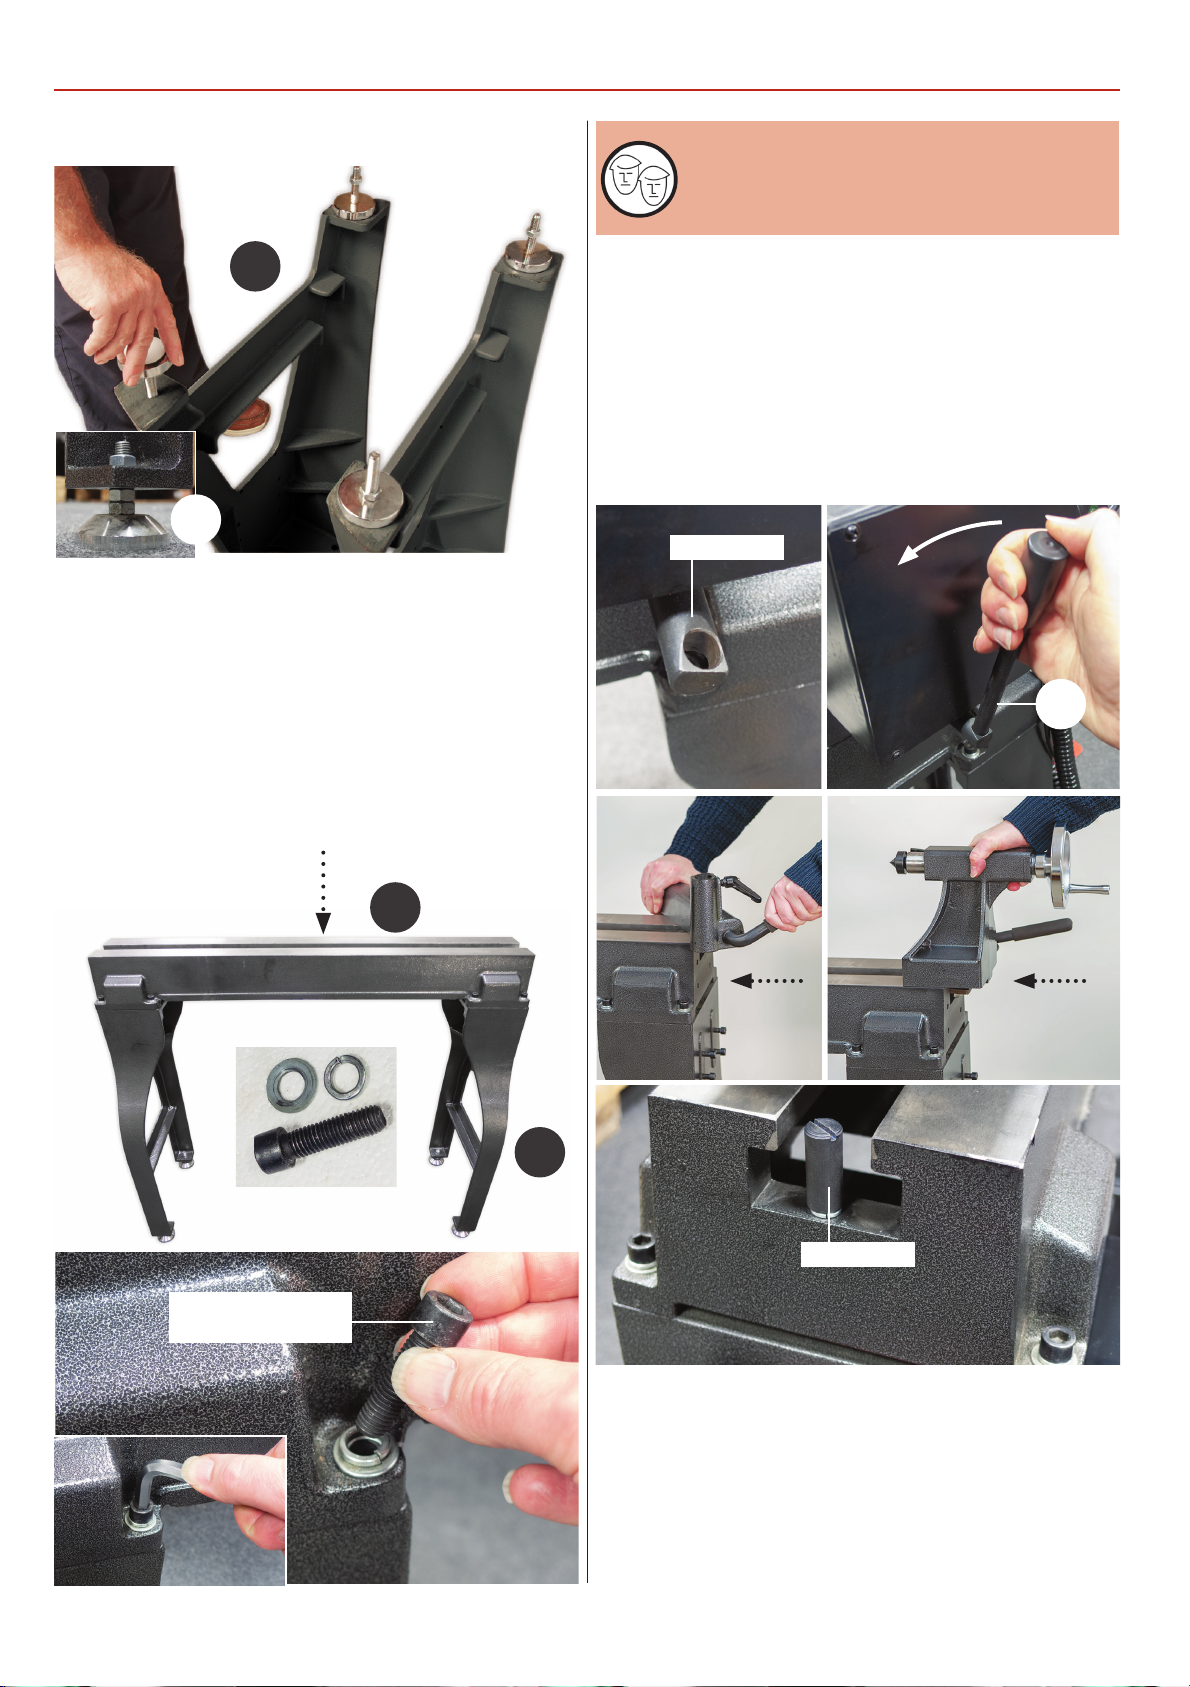
1. Locate the two lathe stands (B) and the four adjustable
feet (C). There should be three nuts on each foot, remove
one nut from the threaded feet. Screw on the threaded
feet into the pre-drilled holes to the base of the stands,
see fig 01. on next page.
5
Continues over...
Page 6
ASSEMBLY
Fig 01
WARNING: THE HEADSTOCK IS HEAVY,
IT IS ADVISABLE TO SEEK HELP.
B
C
2. With the feet attached replace the four nuts you
removed earlier.
3. Place the leg stands on their feet, locate the eight M10
cap head bolts, spring washer/washers.
4. Using a lifting device, or get assistance, lift the lathe
bed (A) up from the floor. Line up the eight machined
holes, four to each end of the lathe bed with the holes in
the leg stands (B) and secure in place with the eight M10
bolts, washers, see fig 02-03.
5. Lift the headstock back onto the lathe bed, line up the
mounting 'T' bracket beneath the headstock with the
machined slot in the centre of the lathe bed and slide the
head on. Locate the headstock locking bar/handle (J). To
the rear of the headstock there is a pivot bar which is part
of the locking mechanism, see fig 05. Slot the bar/handle
(J) through the machined hole in the pivot bar and rotate
anti-clockwise to lock the headstock in place,see fig 06.
Fig 05-06-07-08-09
Pivot bar
J
Fig 02-03-04
M10 Bolt, spring
flat washers
A
B
Stop pin
6. Slide on the tool rest banjo and tailstock assembly and
replace the stop pins to either end of the lathe bed, see
fig 07-08-09.
Tool Storage
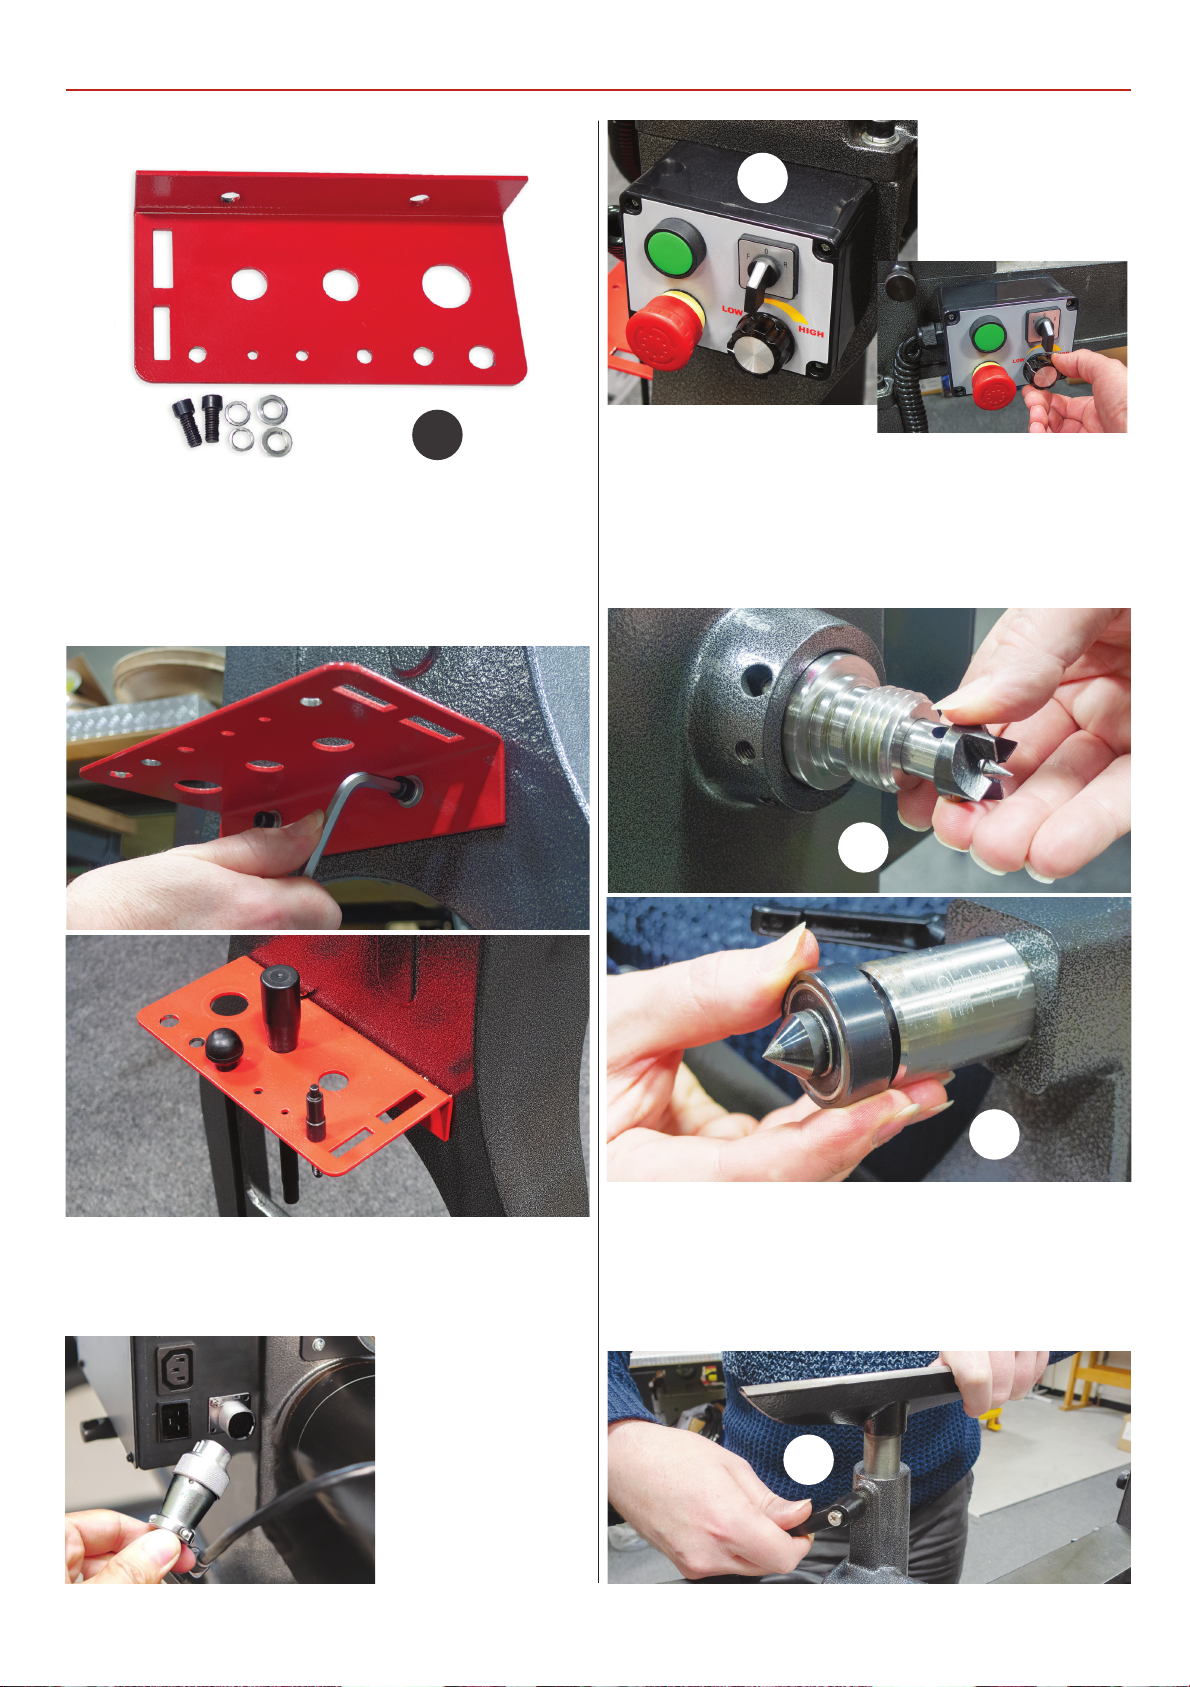
1. Locate the tool storage angle plate and the two
cap head bolts, spring/flat washers (D), see fig 10.
6
Page 7
ASSEMBLY
Fig 10
D
2. Place flat/spring washer over each cap head bolt.
Lineup the two holes in the angle bracket with the holes
in the left lathe stand, below the headstock and secure
in place with the two cap head bolts, see fig 11-12.
Fig 11-12
The switch control box
(L) is magnetised and
L
Four Prong Drive/Live Centre
Locate both drive centres and insert the four prong drive
(G) into the headstock drive shaft and the live centre (H)
into the tailstock barrel, see figs 15-16.
can be positioned anywhere on the lathe for
ease of use, see fig 14.
Fig 15-16
Switch Control Box
Fig 13-14
Locate the switch
control assembly (L).
Connect the male
plug into the female
socket to the rear of
the headstock
assembly, see fig 13.
G
H
Fitting The Tool Rest
Locate the tool rest (F), introduce the tool post into the
banjo and nip-up the locking handle, see fig 17.
Fig 17
F
7
Page 8
ASSEMBLY OPTIONAL ACCESSORIES ASSEMBLY
Motor/Power Cables
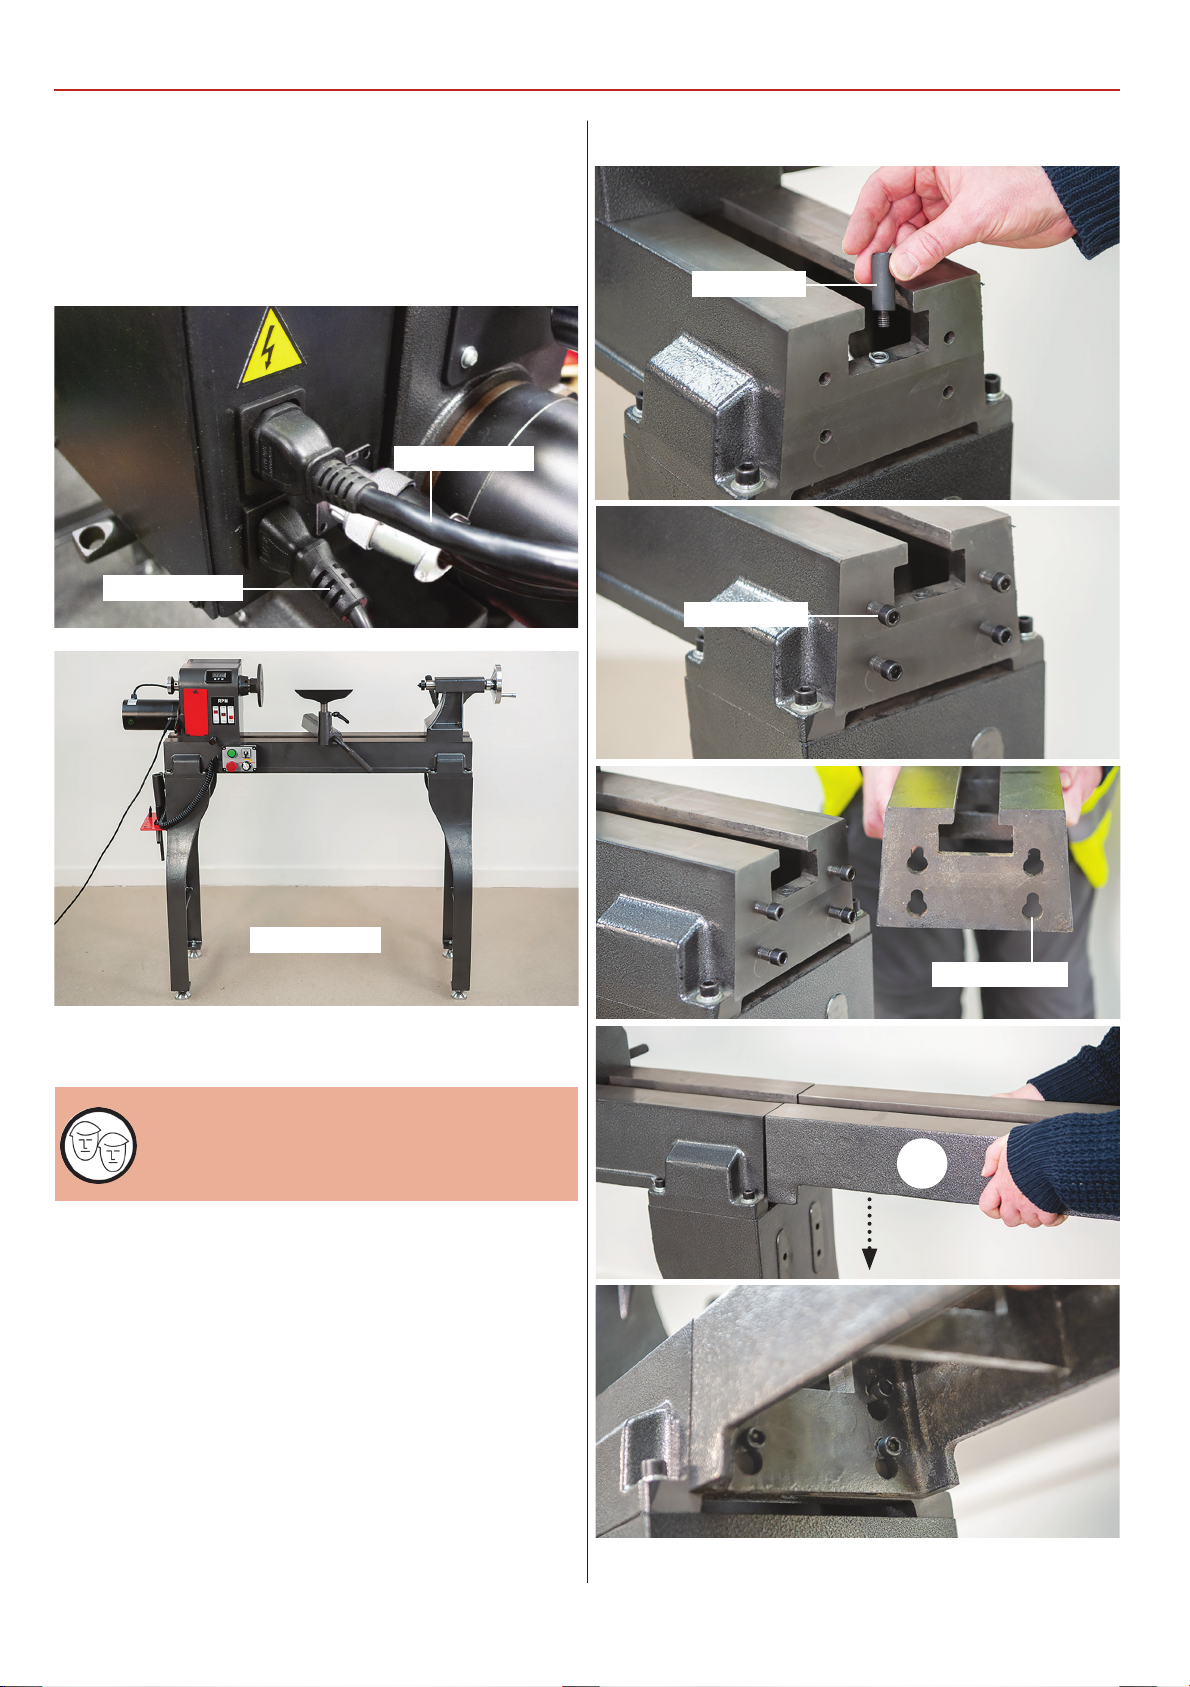
Two the side of the headstock assembly there are two
power sockets. Connect the motor plug to the top socket
and the 230V power cable to the lower socket,see fig 18.
Fig 18
Motor cable
230V cable
Fig 19-20-21-22-23
Stop pin
M10 bolts
Setup 1
Optional Lathe Bed Extension
WARNING: THE BED EXTENSION IS HEAVY, IT IS
ADVISABLE TO SEEK HELP.
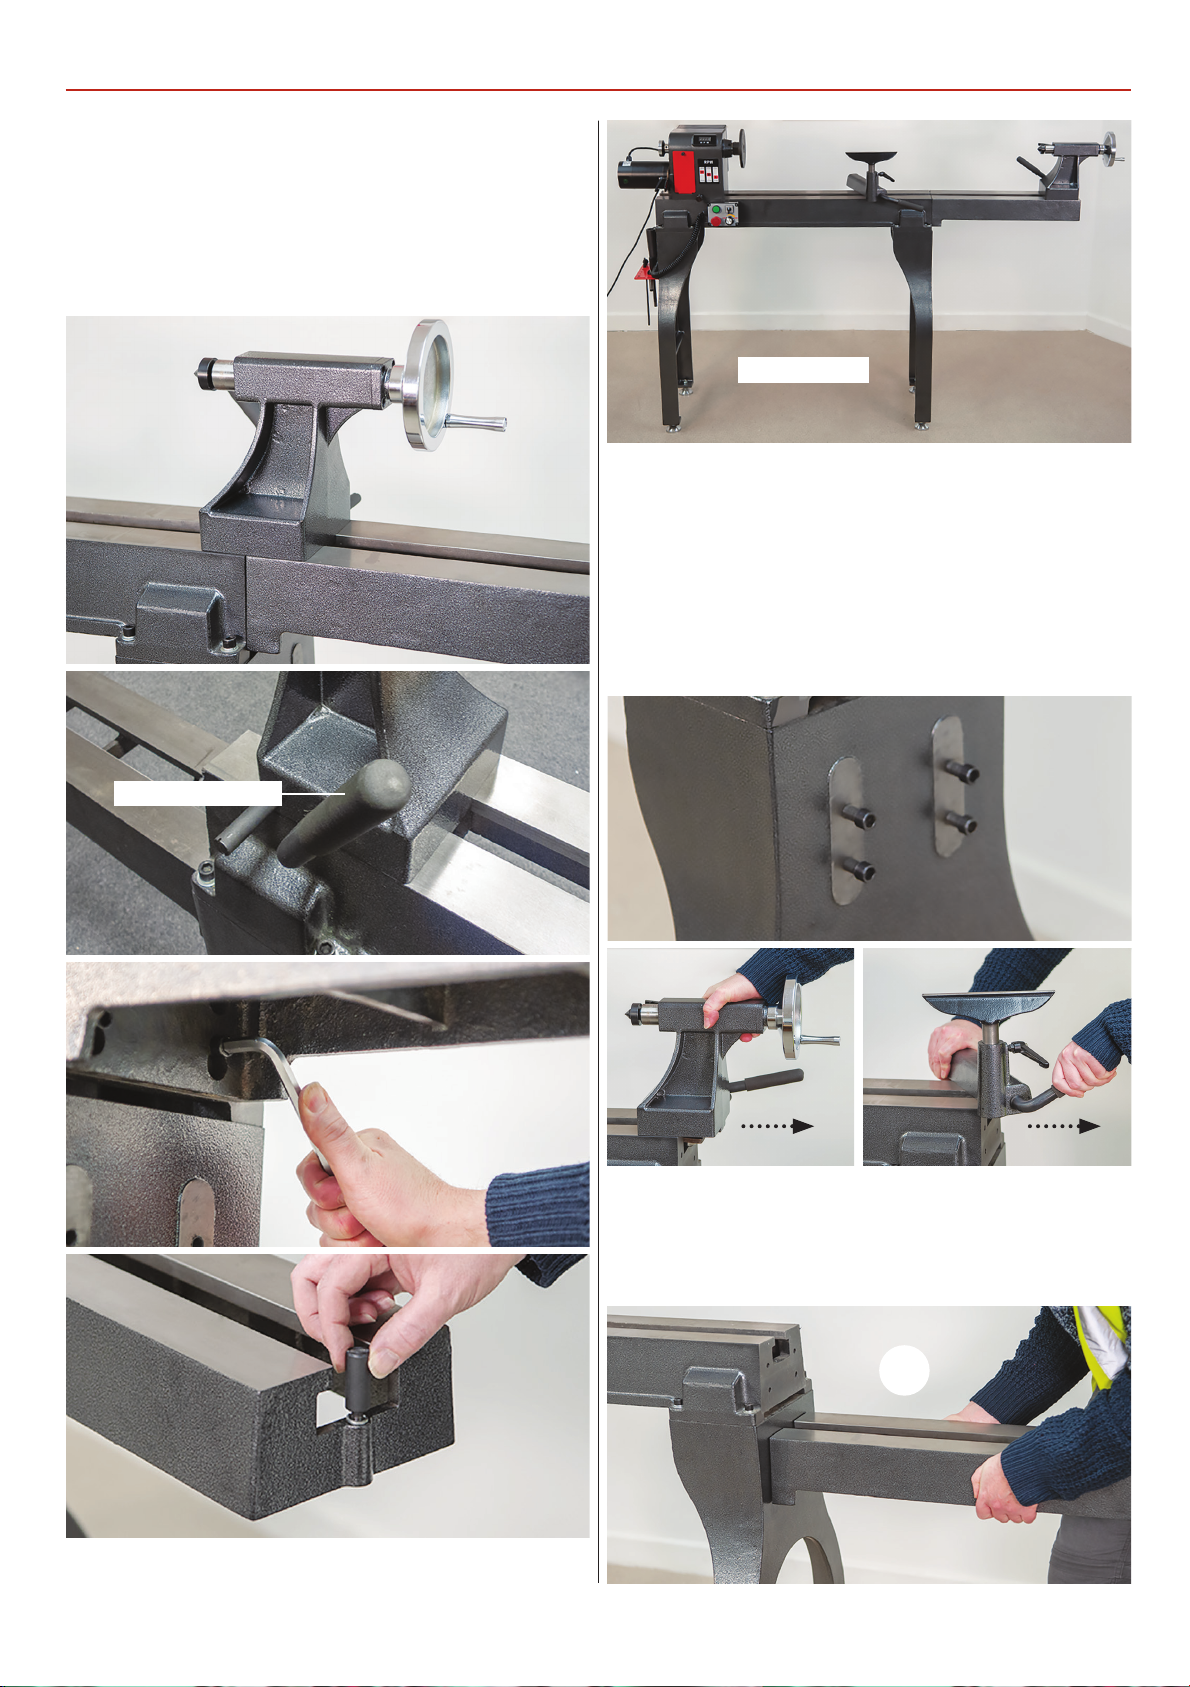
Locate the lathe bed extension (M) and the four cap head
bolts and washers. NOTE: the lathe bed can be mounted
in two positions. The first to the end of the lathe bed and
second mounted to the left leg stand (B) using the four
pre-drilled holes in the casting.
Position One:
1. Remove the tailstock stop pin, to the left side of the
lathe bed. Screw in the four M10 bolts into the four
pre-drilled holes to the end of the lathe bed, see fig 19-20.
Leaving a gap between the bed face and the bolt heads,
lower the key slots in the extension bed (M) down over
the bolts until firmly seated, see fig 21-22-23. NOTE: Don't
tighten at this stage.
Key slots
M
8
Page 9
OPTIONAL ACCESSORIES ASSEMBLY
2. Move the tailstock assembly over both beds and lock in
place using the locking lever. Tighten the bolts beneath
the bed extension (M), both beds should now be level.
If not, repeat the process until achieved. Replace the stop
pin to the end of the lathe extension (M), see fig 24-25-26-
27.
Fig 24-25-26-27
Setup 2
Position Two:
1. Lightly screw in the four M10 bolts into pre-drilled holes
in the left leg stand casting (B), see fig 28 NOTE: leave a
gap between the stand face and bolt heads, ready for the
next step. Remove the tailstock & tool rest banjo and place
aside, see fig 29.
Locking lever
Fig 28-29
2. Lower the extension bed down, until the keyed holes
are firmly seated down over the bolts. Tighten the
cap head bolts to secure the bed in place, see fig 30.
Fig 30
M
9
Continues over...
Page 10
OPTIONAL ACCESSORIES ASSEMBLY
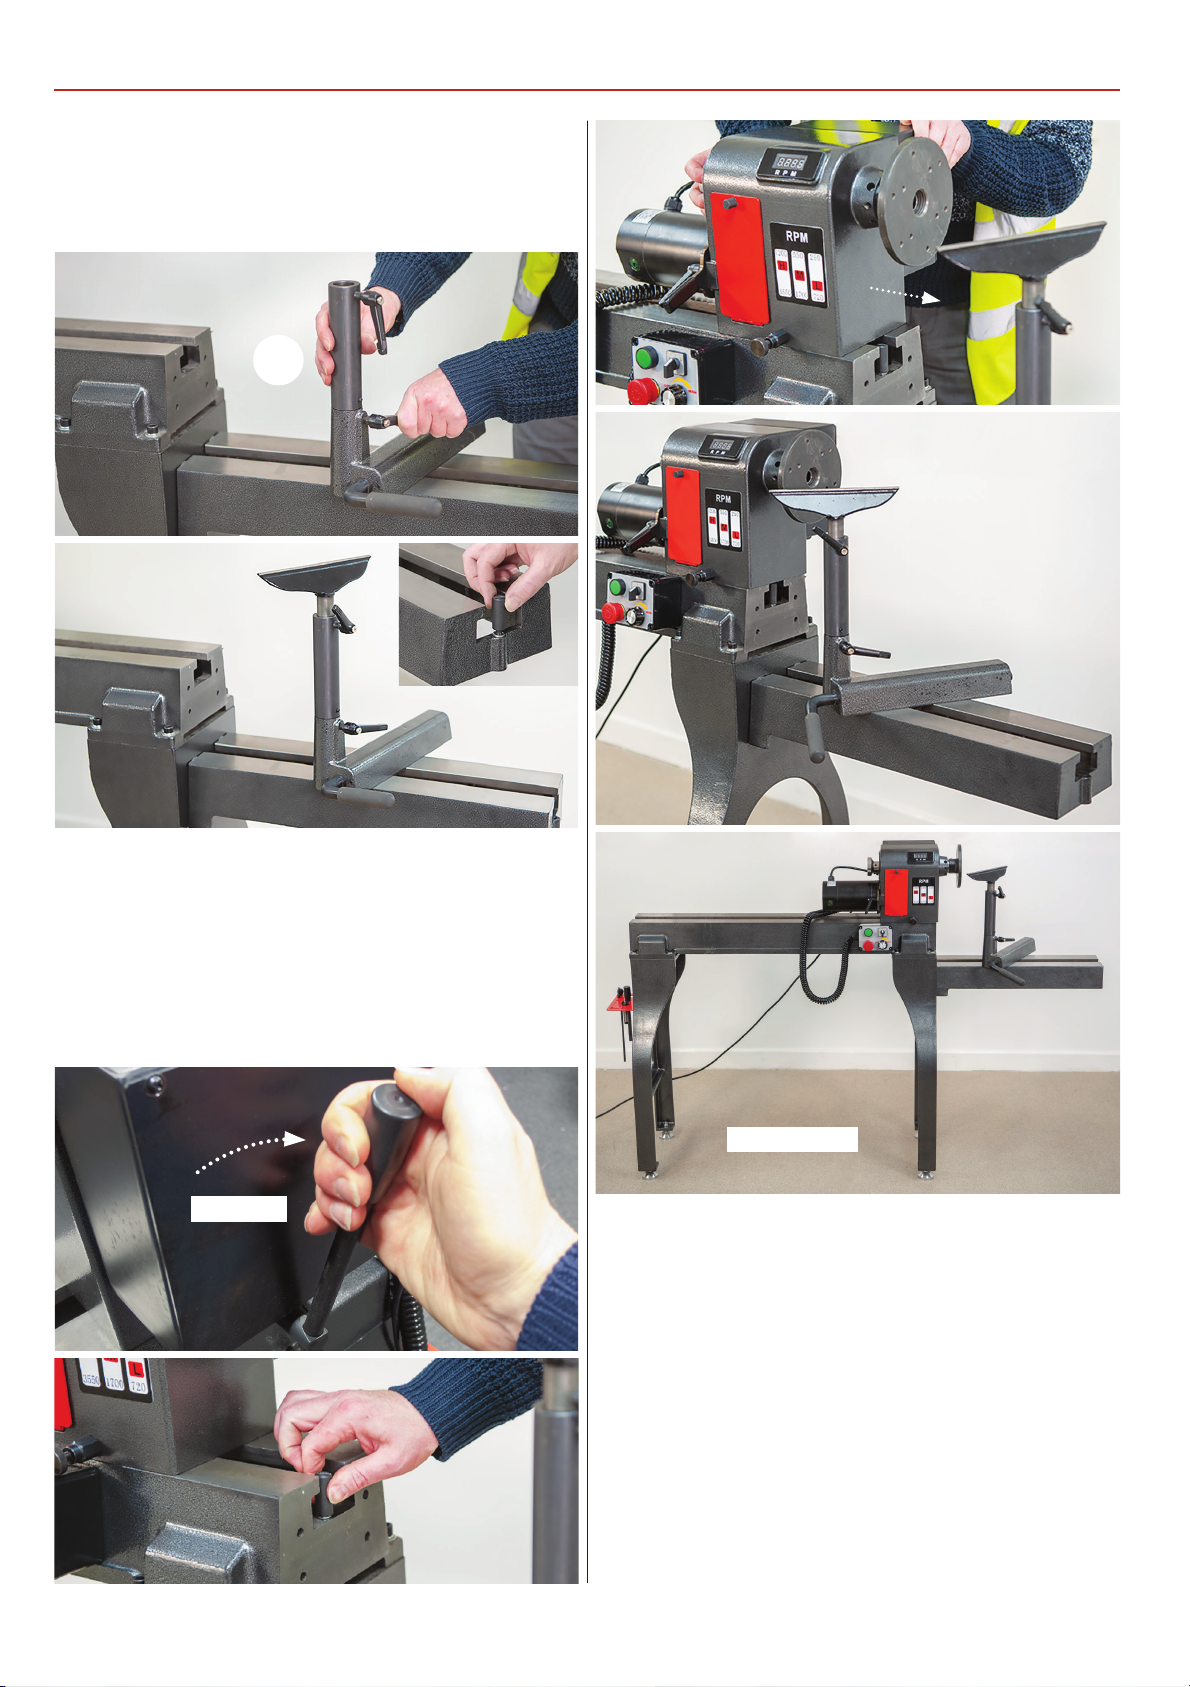
3. Refit the tool rest banjo assembly onto the extension
bed (M), remove the tool rest,locate the tool rest extension
post (N) and install. Refit the tool rest, see fig 31-32.
Fig 31-32
N
4. Replace the stop pin into the thread hole to the end of
the lathe bed extension.
5. Unlock the headstock assembly, see fig 33 slide the
unit down the opposite end of the lathe bed. Replace the
stop pin and lock the headstock against the stop,see fig
34-35-36-37.
Fig 33-34-35-36
Unlock
Setup 3
10
Page 11
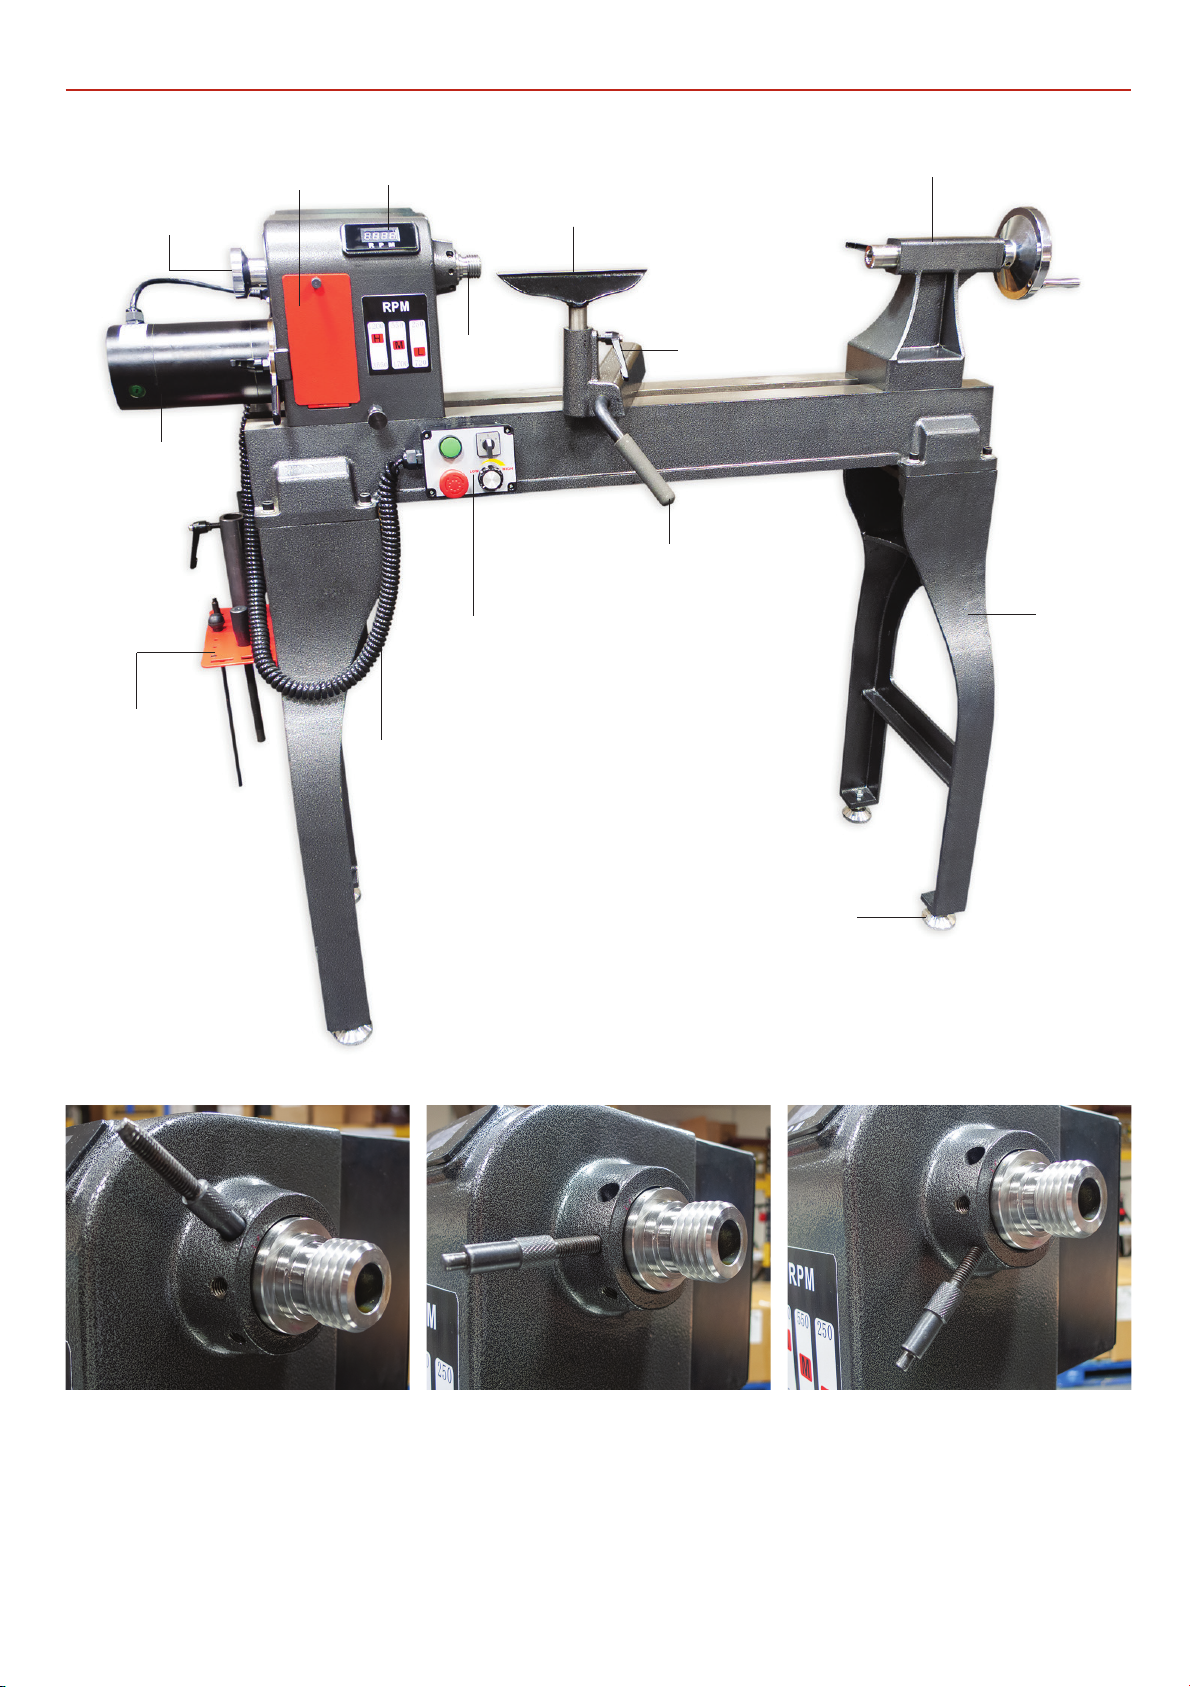
ILLUSTRATION & PARTS DESCRIPTION
Motor pulley
Spindle wheel
Motor
Tool storage
access door
Spindle speed
Digital readout
Tool rest
Spindle
Control switch box
with magnetic base
Switch box flexible cable
Tailstock
Tool rest lock
Banjo locking
handle
Stand
Adjustable foot
• Top hole for 12 point indexing
• There are three machined holes to the right side of the headstock at 40˚degrees apart.
• The spindle circumference has 12 indexing holes at 30˚degrees apart.
• The lathe has a total of 36 indexing position at (10˚) segments.
• Middle threaded hole
for 24 point indexing
• Lower threaded hole
for 36 point indexing
11
Page 12
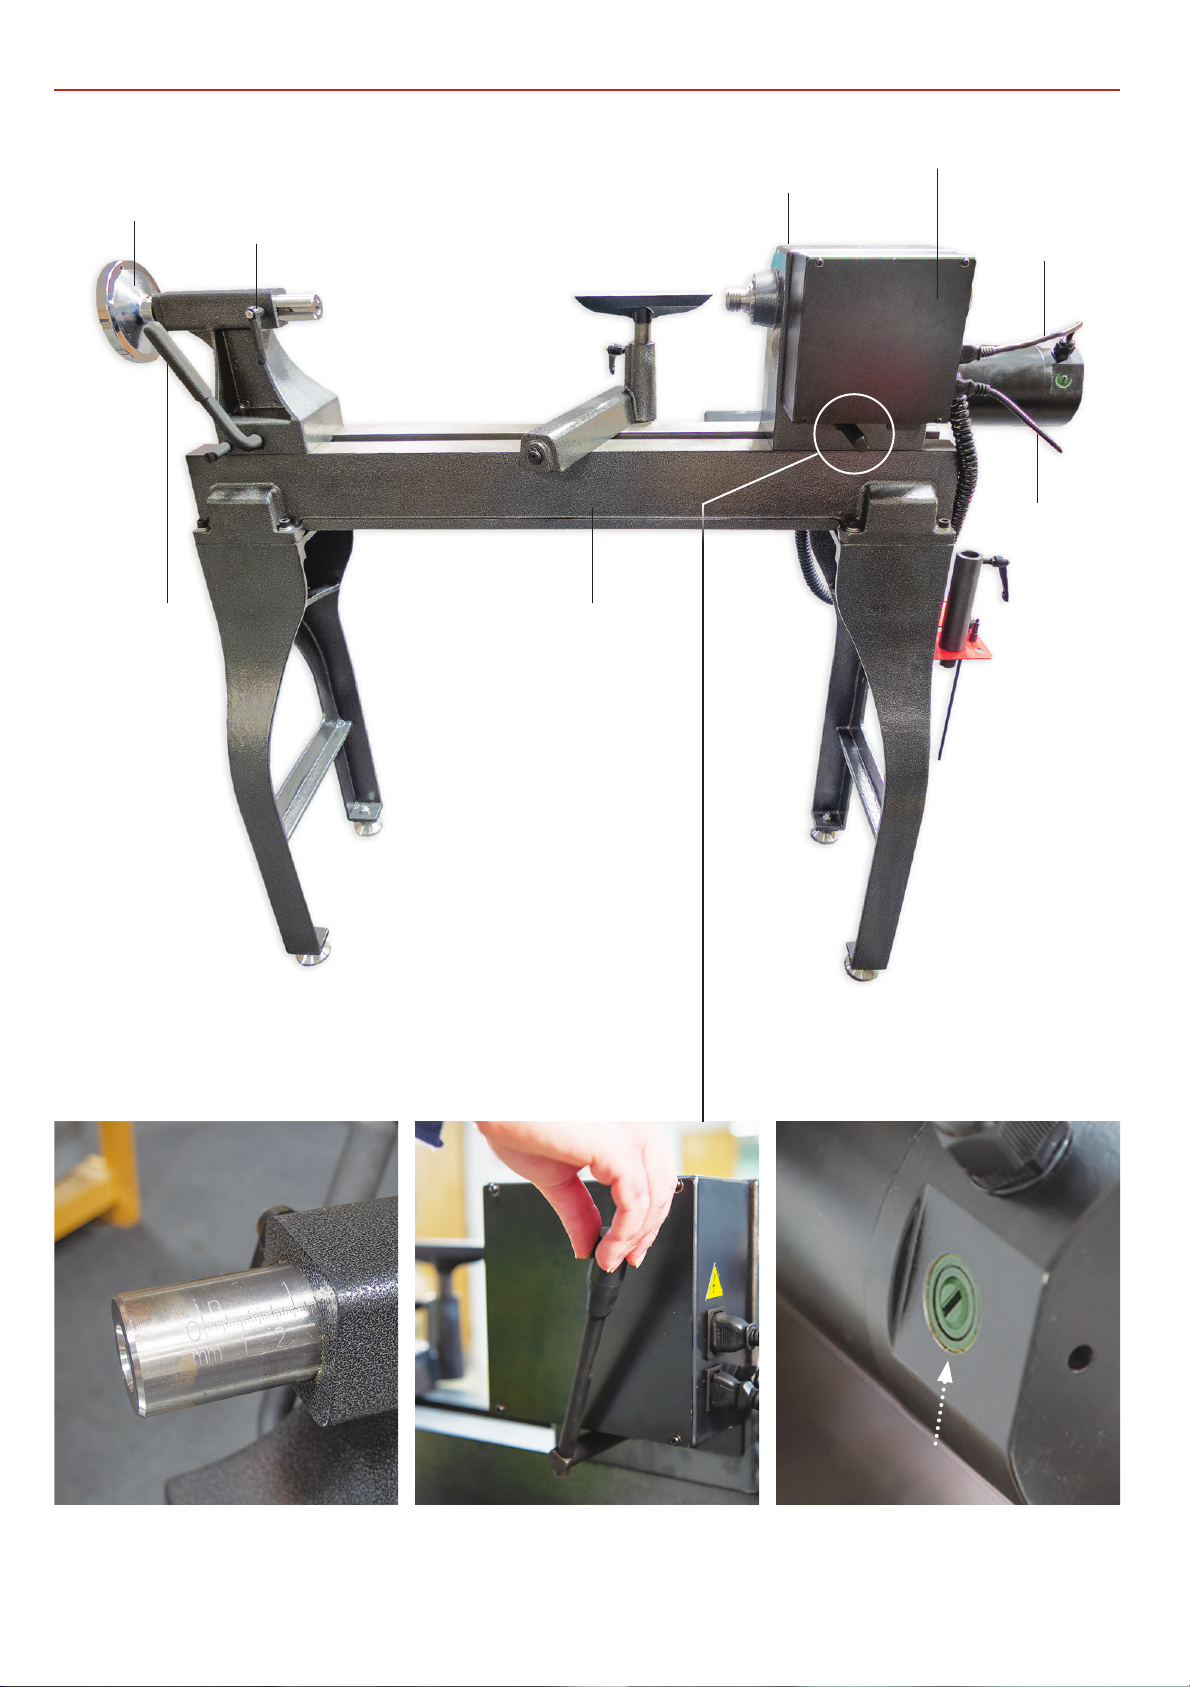
ILLUSTRATION & PARTS DESCRIPTION
Tailstock
wheel
Tailstock barrel lock
Circuit control box
Headstock
Motor cable
Power cable
Locking lever
Lathe bed
Tailstock barrel with
integrated scale
Headstock locking
lever mechanism
12
Motor brush access port
Page 13
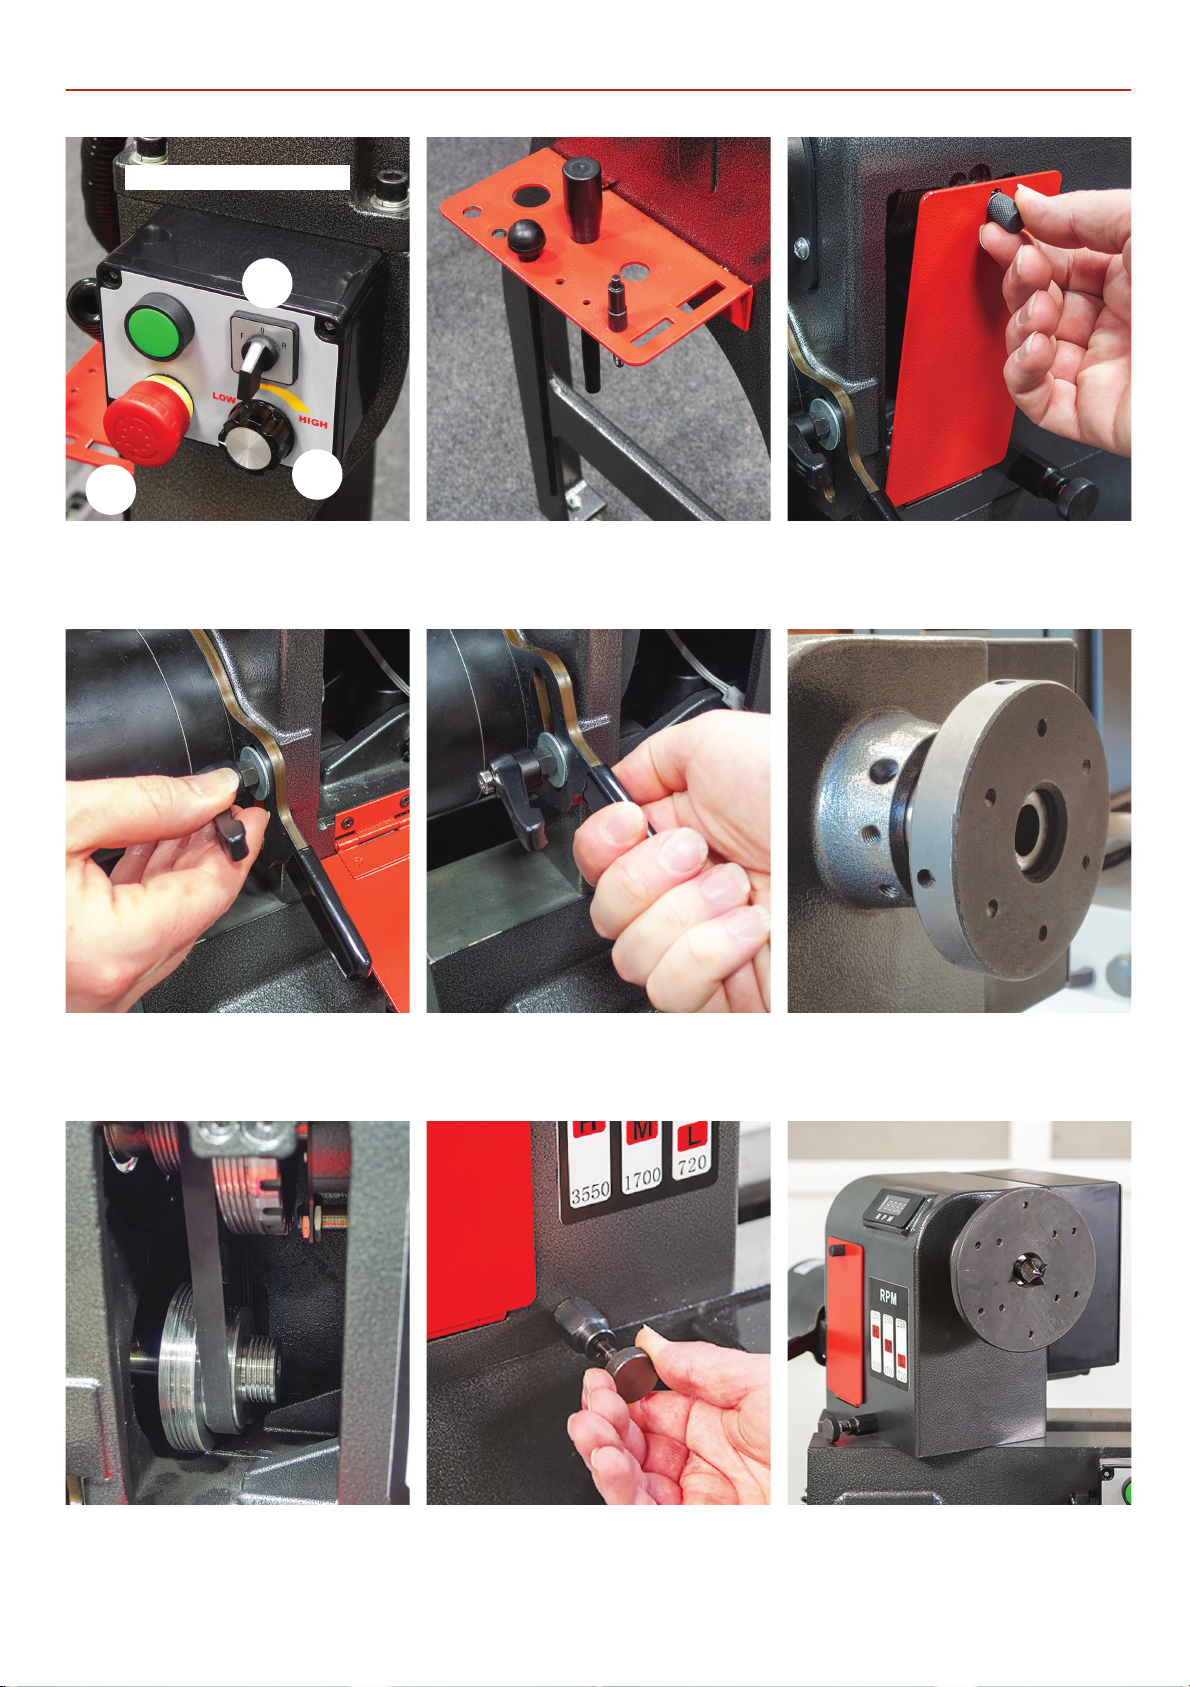
Switch control box
A
ILLUSTRATION & PARTS DESCRIPTION
C
Forward/Reverse switch (A)
Speed control dial (B)
Emergency stop (C)
Motor locking handle Motor operating handle 102mm (4inch) Faceplate
B
Tool storage bracket Drive pulley access door
Motor and spindle drive pulleys Pull out the pivot lock pin to rotate the headstock around with
four preset angles, 60˚- 90˚- 120˚ and 180˚ degrees
13
Page 14
OPERATING INSTRUCTIONS
DISCONNECT THE LATHE FROM THE MAINS
SUPPLY BEFORE CONTINUING!
Fitting & Removing the Faceplate
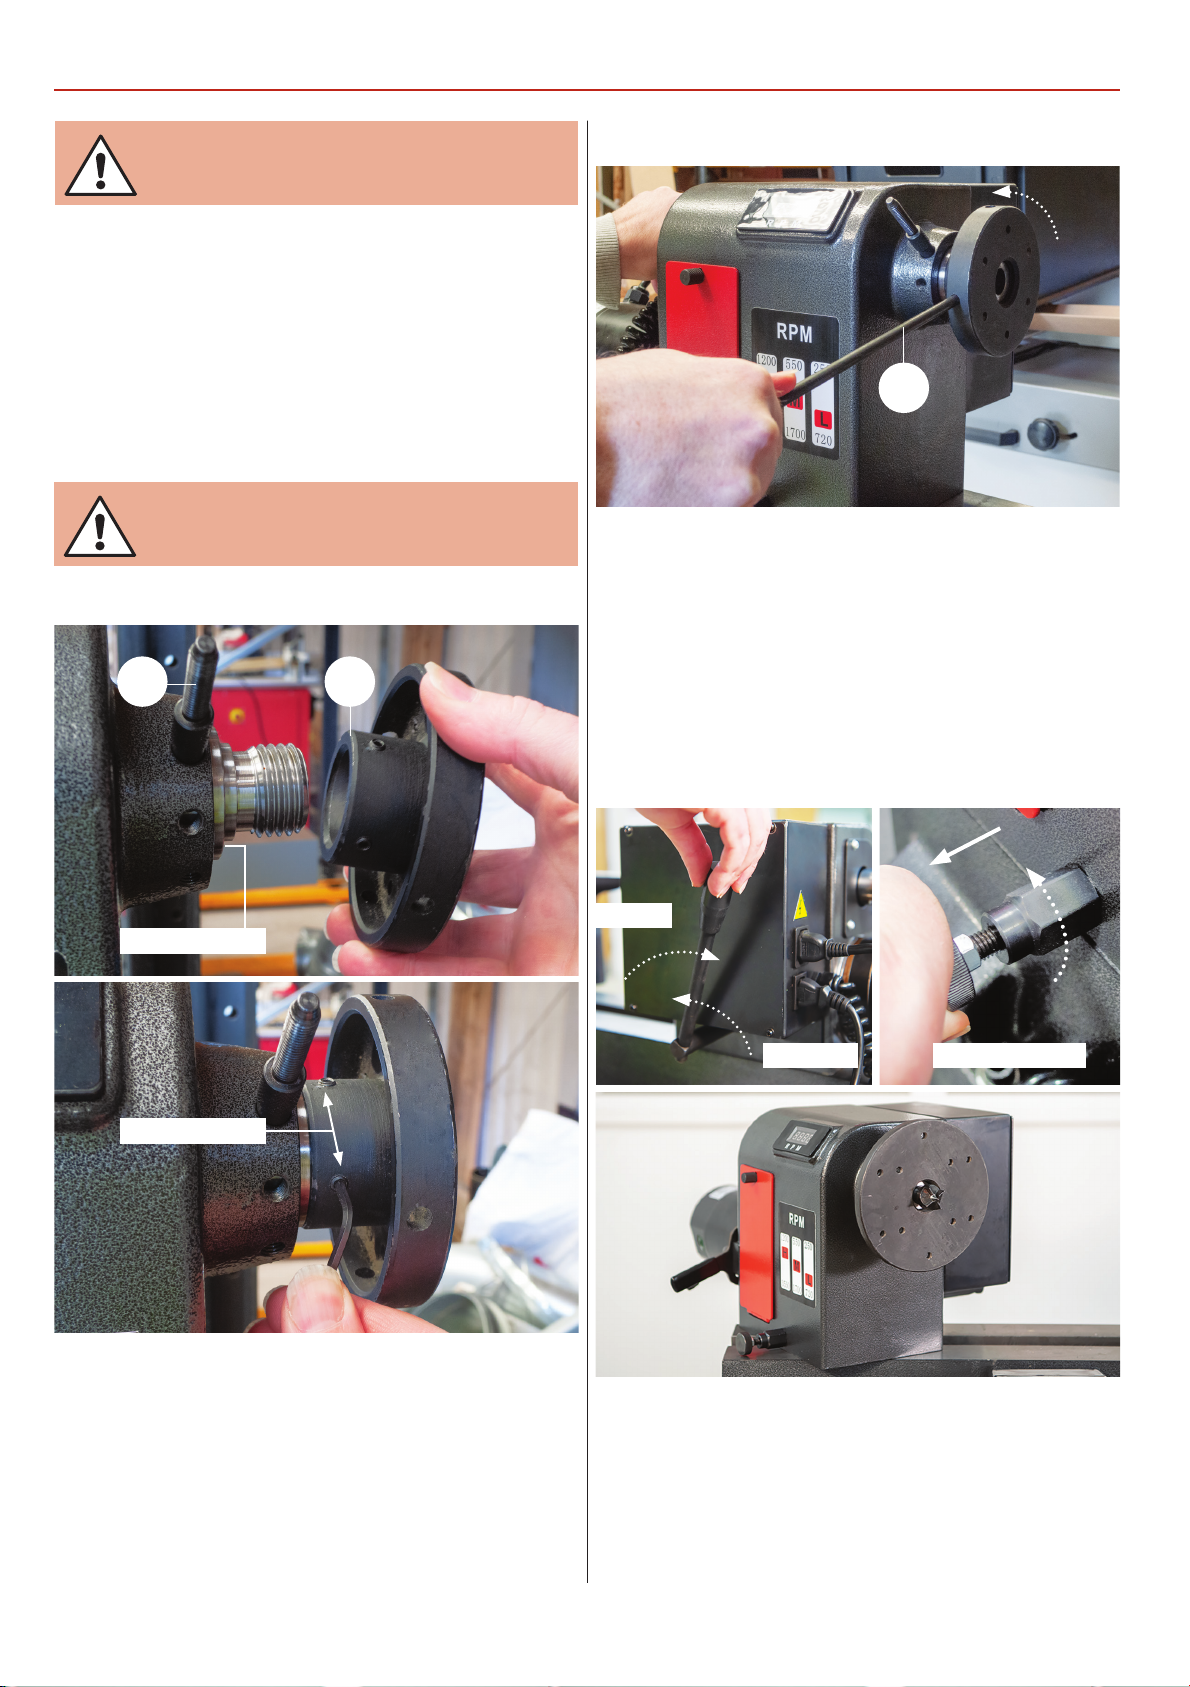
1. Locate the index pin (I), rotate the spindle until one of
the holes lines up with the top hole in the headstock.
Insert the pin to lock the spindle. Find the 4 inch
(102mm) faceplate (E) and screw the threaded boss
onto the spindle thread (M33x3.5), see fig 38. Using a Hex
key nip-up the two grub screws on the boss to secure the
faceplate, see fig 39. Remove the indexing pin and place
safely away.
MAKE SURE FACEPLATE BOSS IS UP AGAINST
THE SPINDLE REGISTER TO PREVENT THE GRUB
SCREWS FROM DAMAGING THE SPINDLE THREAD!
Fig 38-39
I E
Fig 40
K
Rotating the Headstock
The headstock has four preset stop angles, 60˚- 90˚- 120˚
and 180˚degrees.
1. Un-lock the headstock locking lever to the rear, turn
and pull the pivot pin out, see fig 41 rotate the headstock
to the first preset stop at 60˚, the pin will automatically
re-engage to lock the headstock in place, see fig 42.
Register
Grub screws
2. To remove the plate, lock the spindle with the index pin
and loosen the two grub screws on the threaded boss.
NOTE: make sure to unscrew the grub screws enough to
prevent them form jamming and damaging the spindle
thread when removing the faceplate.
3. Introduce the push rod shaft (K) into the machined
hole in the faceplate to act as a lever. Press down to
release the Faceplate from the spindle, see fig 40.
Fig 41-42
Lock
Un-lock
Pivot pin lock
60˚
2. Pull the pivot pin out and carry on rotating to the other
preset stops, see fig 43-44-45. Once the required angle is
reached, turn the locking lever to secure the headstock.
NOTE: the lathe comes with a 4 inch (102mm)
faceplate as standard, the following pictures show a
6 inch (152mm) faceplate attached, not included.
14
Page 15
OPERATING INSTRUCTIONS
Fig 43-44-45
90˚
120˚
Fig46-47-48-49-50
1
2
180˚
KEEP WORK AREA AS UNCLUTTERED AS IS
PRACTICAL. UNDER NO CIRCUMSTANCES SHOULD
CHILDREN BE ALLOWED IN WORK AREAS.
CONNECT THE LATHE TO THE MAINS SUPPLY
BEFORE CONTINUING!
Switch Control Box
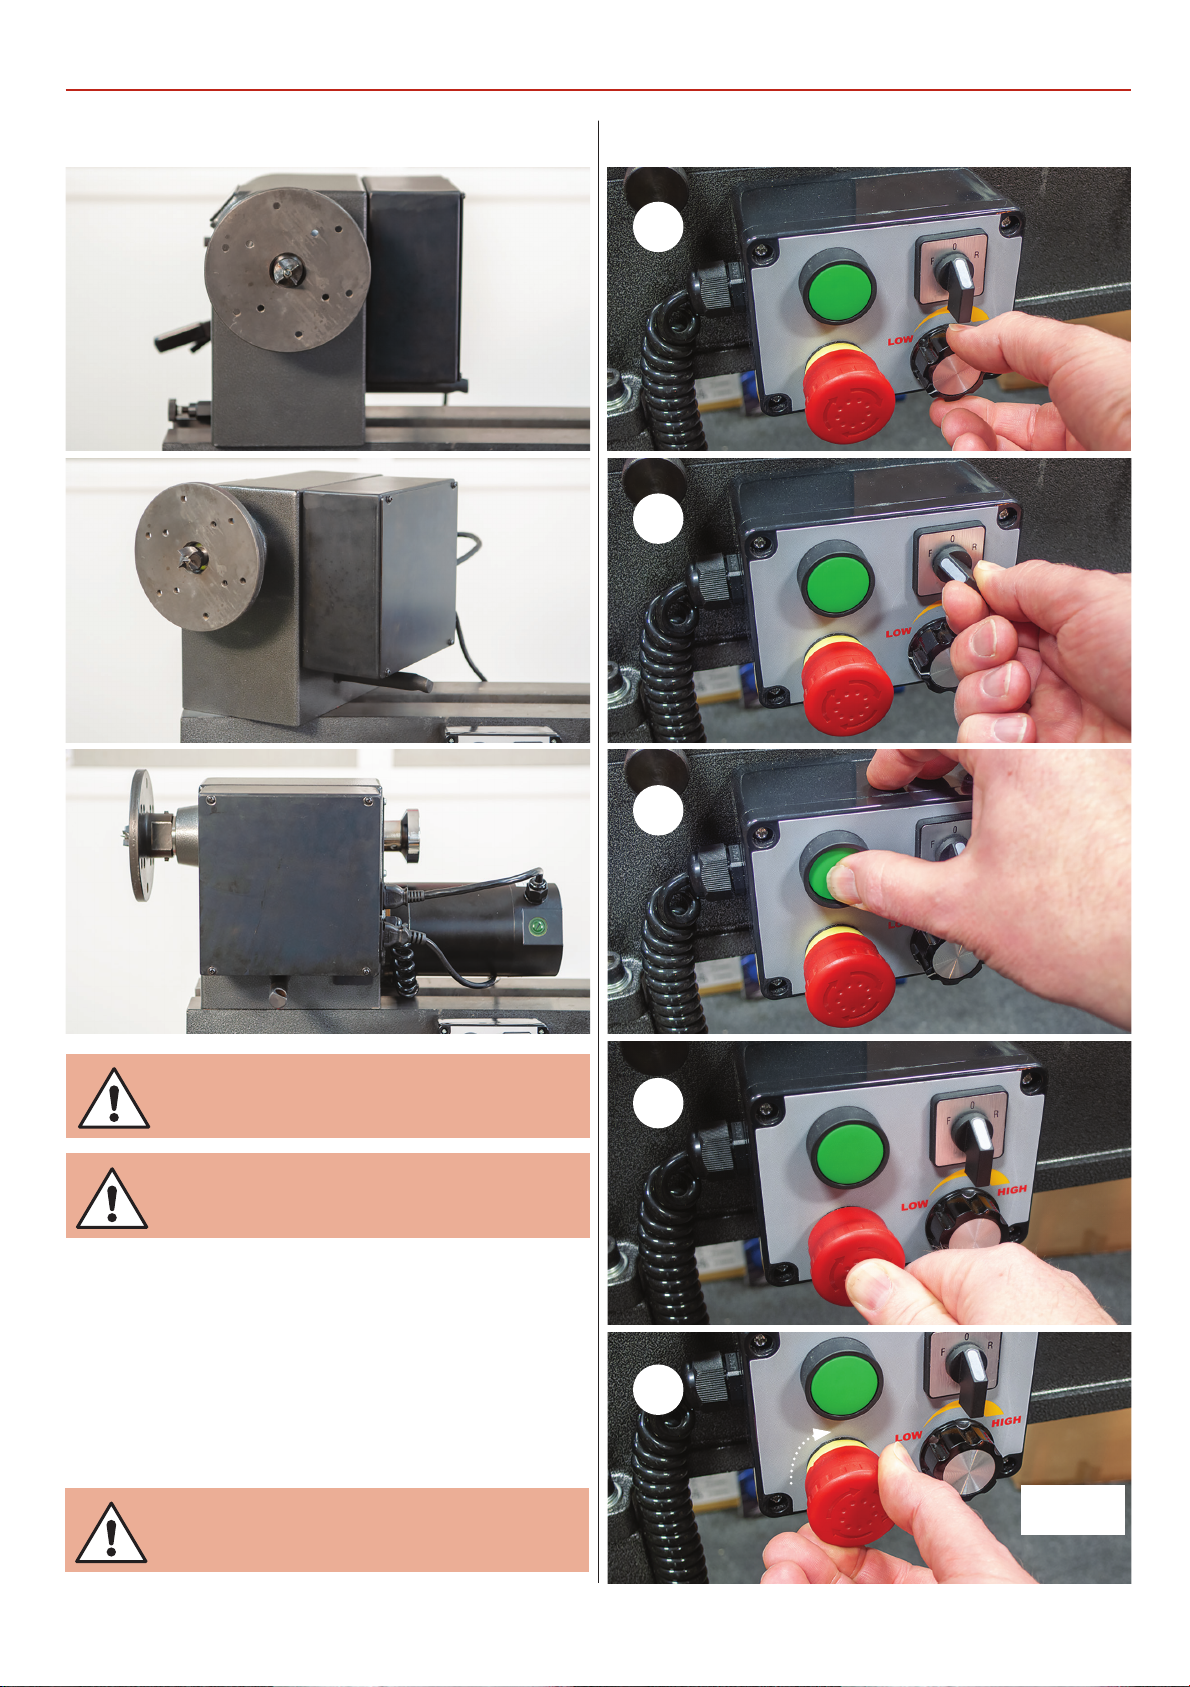
Turn the speed control dial down to the lowest setting.
Twist the selector switch to the forward/reverse position
and press the 'GREEN' button to start the lathe. Turn the
speed control dial to select the speed required. Once
finished turn the speed right down and press the
emergency stop/ off button to stop the lathe. Disconnect
the lathe from the mains supply, see figs 46-47-48-49-50.
3
4
5
WARNING! DO NOT MOVE THE FORWARD
REVERSE SWITCH WHILE THE LATHE IS IN
MOTION.
Twist to
un-lock
15
Page 16
OPERATING INSTRUCTIONS
DISCONNECT THE LATHE FROM THE MAINS
SUPPLY BEFORE CONTINUING!
Indexing Facility
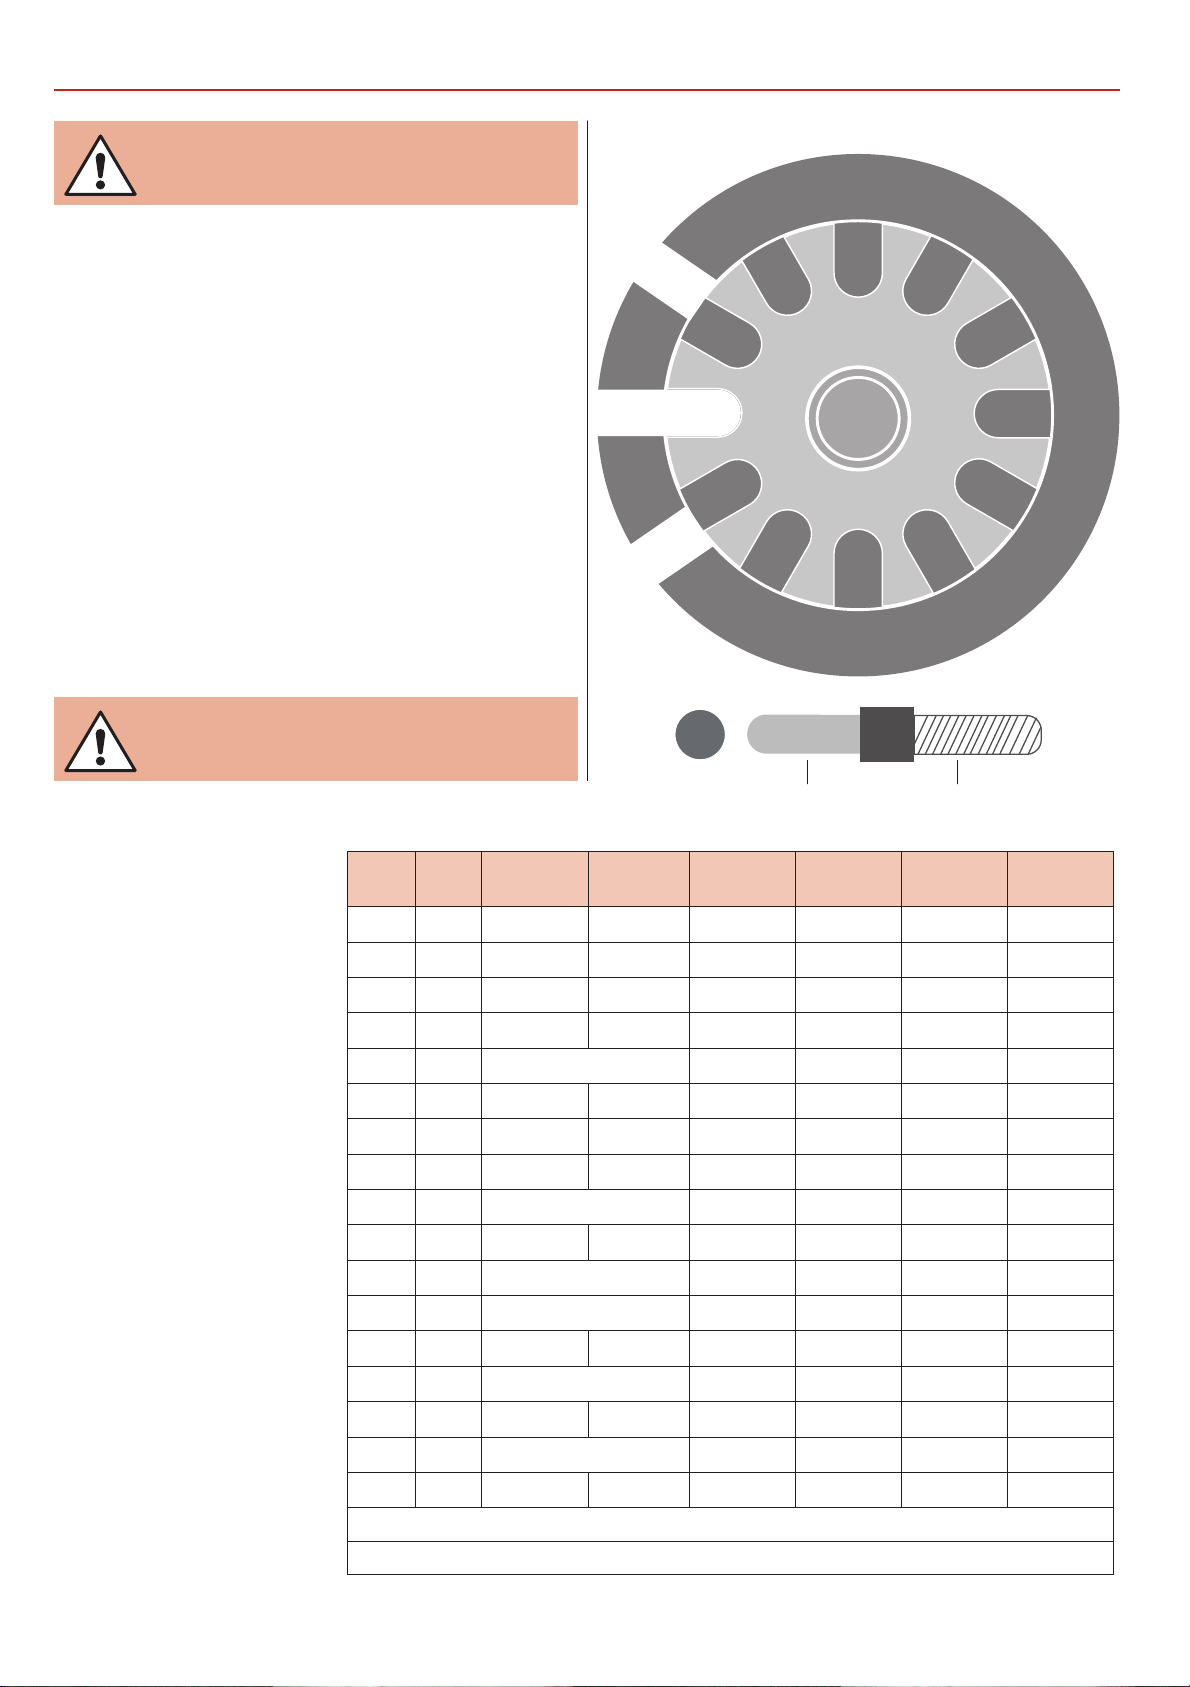
Indexing is an operation of dividing the circumference
of a cylindrical workpiece into equal number of divisions.
The lathe allows 36 indexed positions at 10˚divisions. The
indexing facility is useful for fluted columns, clock faces
and accurate hole positioning.
B
10
Headstock
12
11
Spindle
1
2
The diagram as shown is viewed looking from the
tailstock end of the lathe. There are three holes in the
headstock (A, B, C), 40˚ degrees apart, to accept the
indexing pin (I). The spindle collar has 12 equally spaced
holes around its circumference, 30˚degree apart. They
are numbered 1 through 12.
Hole (B) in the headstock casting is for 12 point indexing,
the middle hole (A) is for 24 point indexing and hole (C) is
for 36 point indexing. NOTE: Holes (A & C) are threaded
and hole (B) is smooth bore.
CAUTION! NEVER START THE LATHE WITH
THE INDEX PIN ENGAGED IN THE SPINDLE.
Indexing ChartExample
If you wish to create 9 flutes
on your spindle workpiece,
use the indexing chart and
find '9' in the 'No. Flutes'
column. Each flute angle will
be 40˚degrees. The index
pin (I) should first be inserted
into the hole combination
'A-1'. Make your first flute at
this position. Remove the
indexing pin and rotate the
spindle until the index pin
can be inserted into hole
combination 'A-5'; this will
be followed by 'A-9'. The
succeeding flutes will be
made with the index pin in
the 'B' position, 'B-3', B-7'
and so on.
No.
Angle Headstock
Flutes
1 360˚ A 1
2 180˚ A 1-7
3 120˚ A 1-5-9
4 90˚ A 1-4-7-10
5 72˚ ------------------
6 60˚ A 1-3-5-7-9-11
8 45˚ A 1-4-7-10
9 40˚ A 1-5-9 B
10 36˚ ------------------
12 30˚ B 1-12
15 24˚ ------------------
16 22.5˚ ------------------
Hole
A
C
Spindle
Number
9
8
7
4
5
6
I
Smooth pin Threaded pin
Headstock
Hole
Spindle
Number
3-7-11 C 1-5-9
Headstock
Hole
3
Spindle
Number
18 20˚ A 1-3-5-7-9-11 B 1-3-5-7-9-11
20 18˚ ------------------
24 15˚ A 1 to 12
30 12˚ ------------------
36 10˚ A 1 to 12 B 1 to 12
NOTE: A dashed line indicates that particular set of angles is not possible with the indexer
C
C
1-3-5-7-9-11
1 to 12
16
Page 17
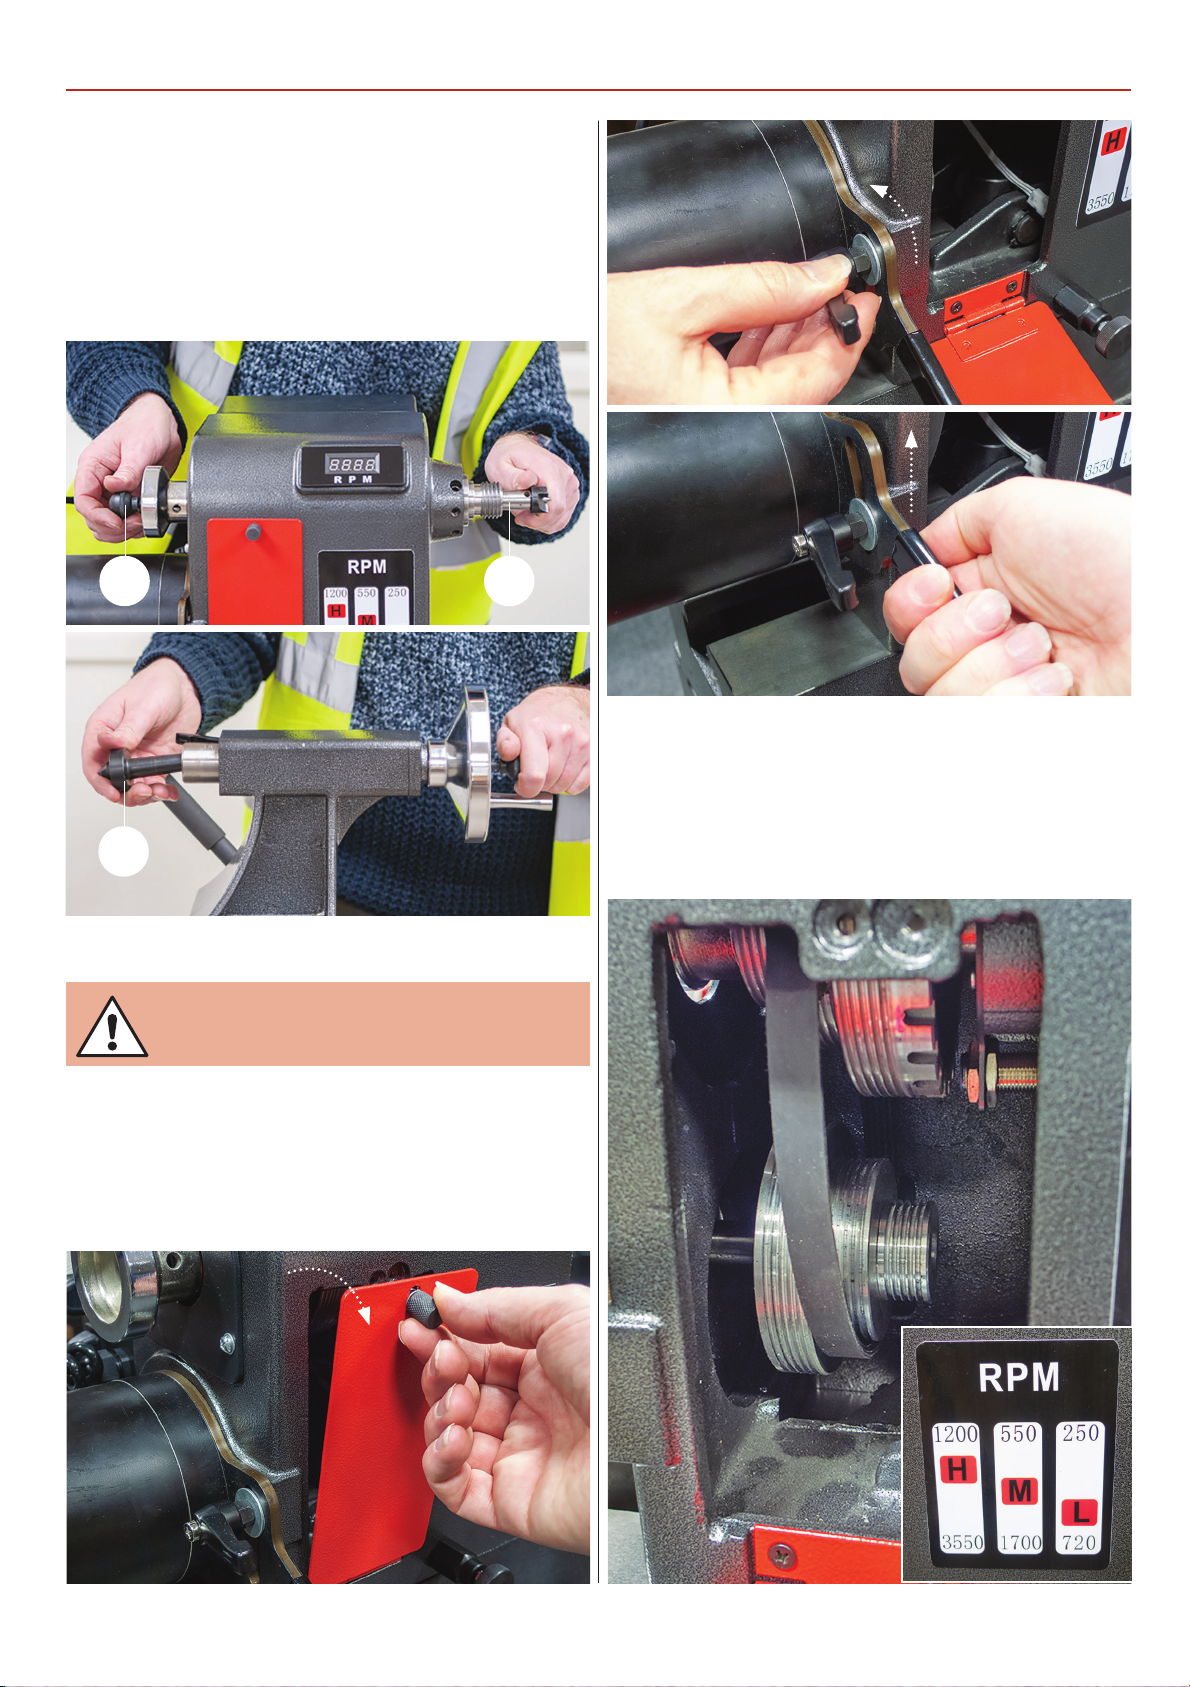
Removing the Drive & Live Centres
To remove the four prong drive (G), insert the push rod (K)
through the centre of the headstock spindle and push
out the 2MT drive, see fig 51. Repeat the procedure to
remove the live centre (H) from the tailstock barrel, see fig
52.
Fig 51-52
GK
OPERATING INSTRUCTIONS
H
Changing the Belt Speed
DISCONNECT THE LATHE FROM THE MAINS
SUPPLY BEFORE CONTINUING!
1. Open the drive pulley access door by unscrewing the
locking knob. Lower the door down, release the motor
locking handle and raise the motor up to release the
tension from the drive belt, see fig 53-54-55.
Fig 53-54-55
2. Look at the speed chart diagram to the front of the
headstock, reposition the drive belt on the motor and
spindle pulleys to the required speed. NOTE: make
sure the grooves in the belt slot into the grooves in
the pulleys, see fig 56-57.
Fig 56-57
17
Continues over...
Page 18
OPERATING INSTRUCTIONS
Fig 58
Fig 59
B
I
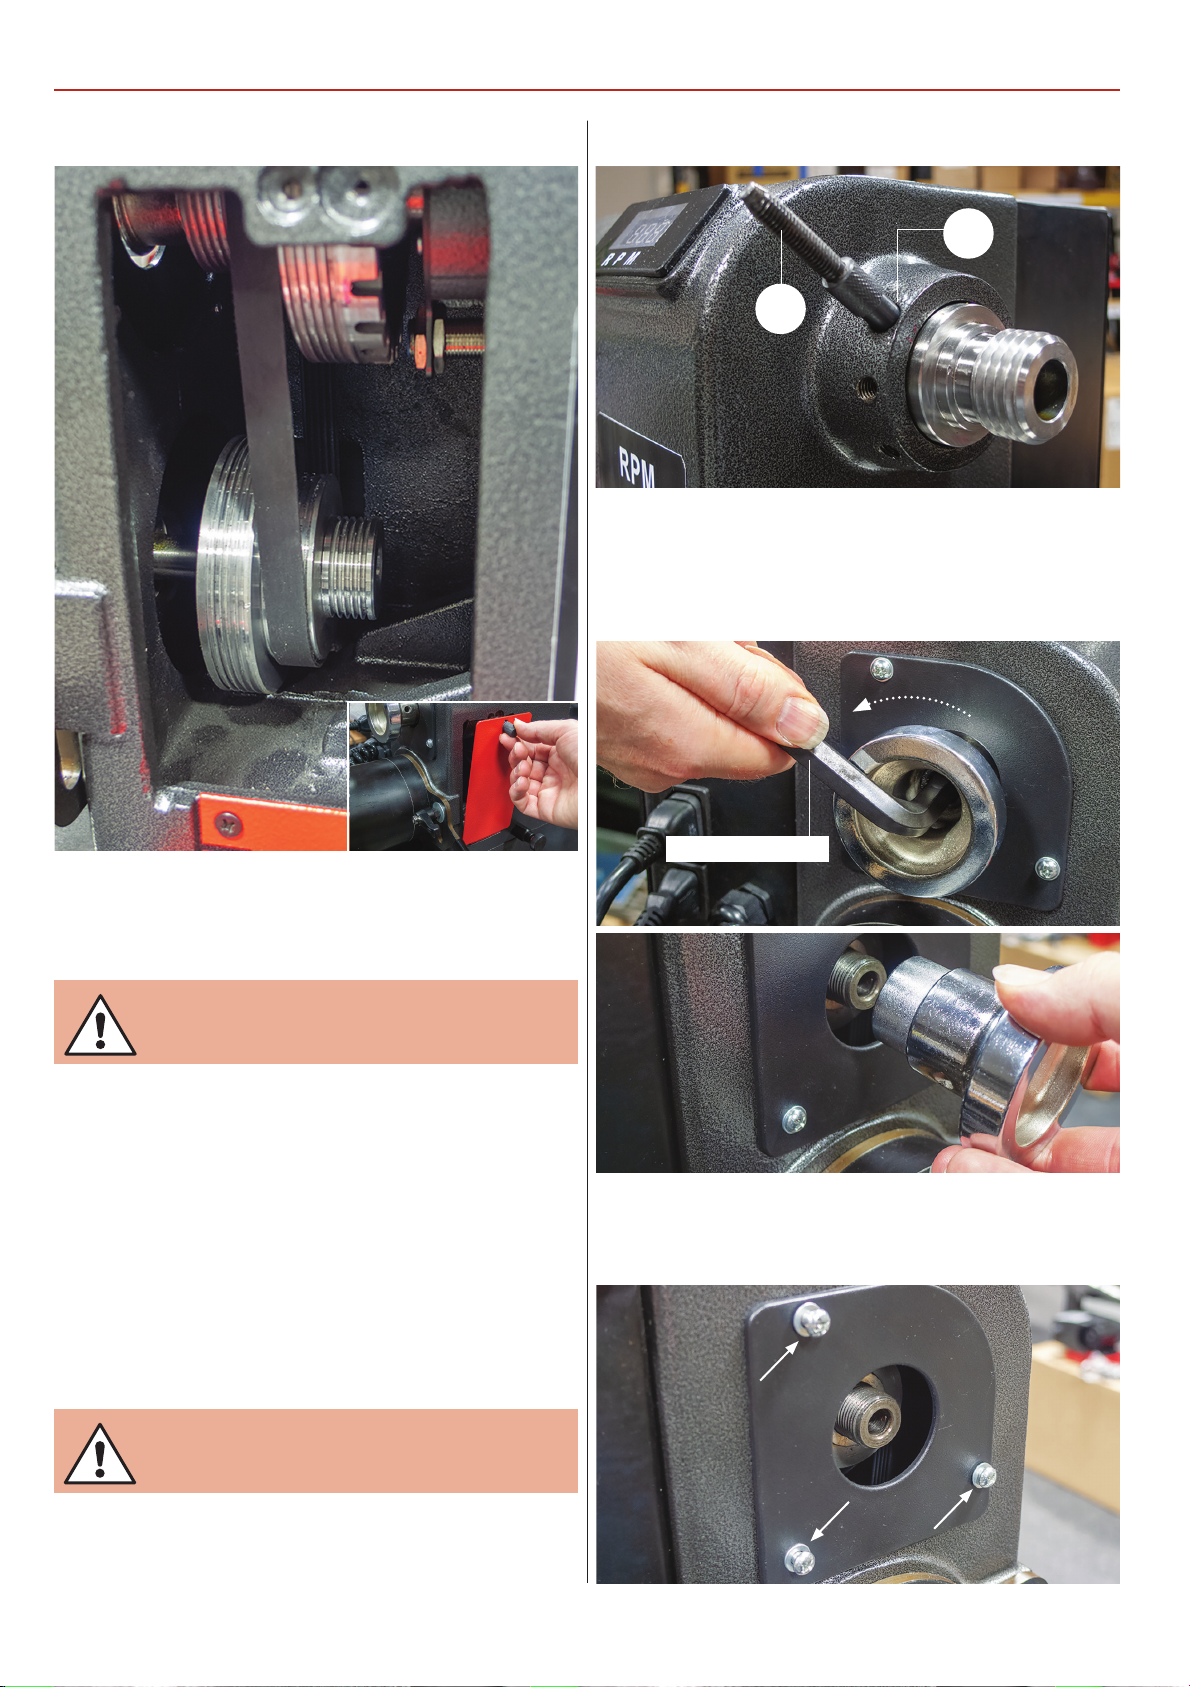
2. Using a 12mm Hex key loosen the headstock wheel.
Unscrew the wheel from spindle assembly and place
safely to one side, see fig 60-61.
Fig 60-61
3. Press down the motor assembly to retention the drive
belt with a slight defection, nip-up the locking handle to
secure the motor. Close the drive pulley access door and
lock in place, see fig 58.
CONNECT THE LATHE TO THE MAINS SUPPLY!
4. Start the lathe and increase the speed, check
everything is running correctly, no vibrations or
knocking sound for example. If everything is fine,
switch off the lathe and wait until the machine comes
to a complete stop.
5. Continue with operation.
Replacing the Drive Belt
Over a period of time check the drive belt for signs of
fraying, splitting or missing teeth. If any of the following
is evident, the belt will need replacing.
12mm Hex key
3. Remove the three screws holding Faceplate and place
it and the screws safely to one side, see fig 62-63.
Fig 62-63
DISCONNECT THE LATHE FROM THE MAINS
SUPPLY BEFORE CONTINUING!
1. Open the drive pulley access door, insert the indexing
pin (I) into the top indexing hole (B) to the right side of
the headstock, locking the spindle in place, see fig 59.
18
Page 19
OPERATING INSTRUCTIONS MAINTENANCE
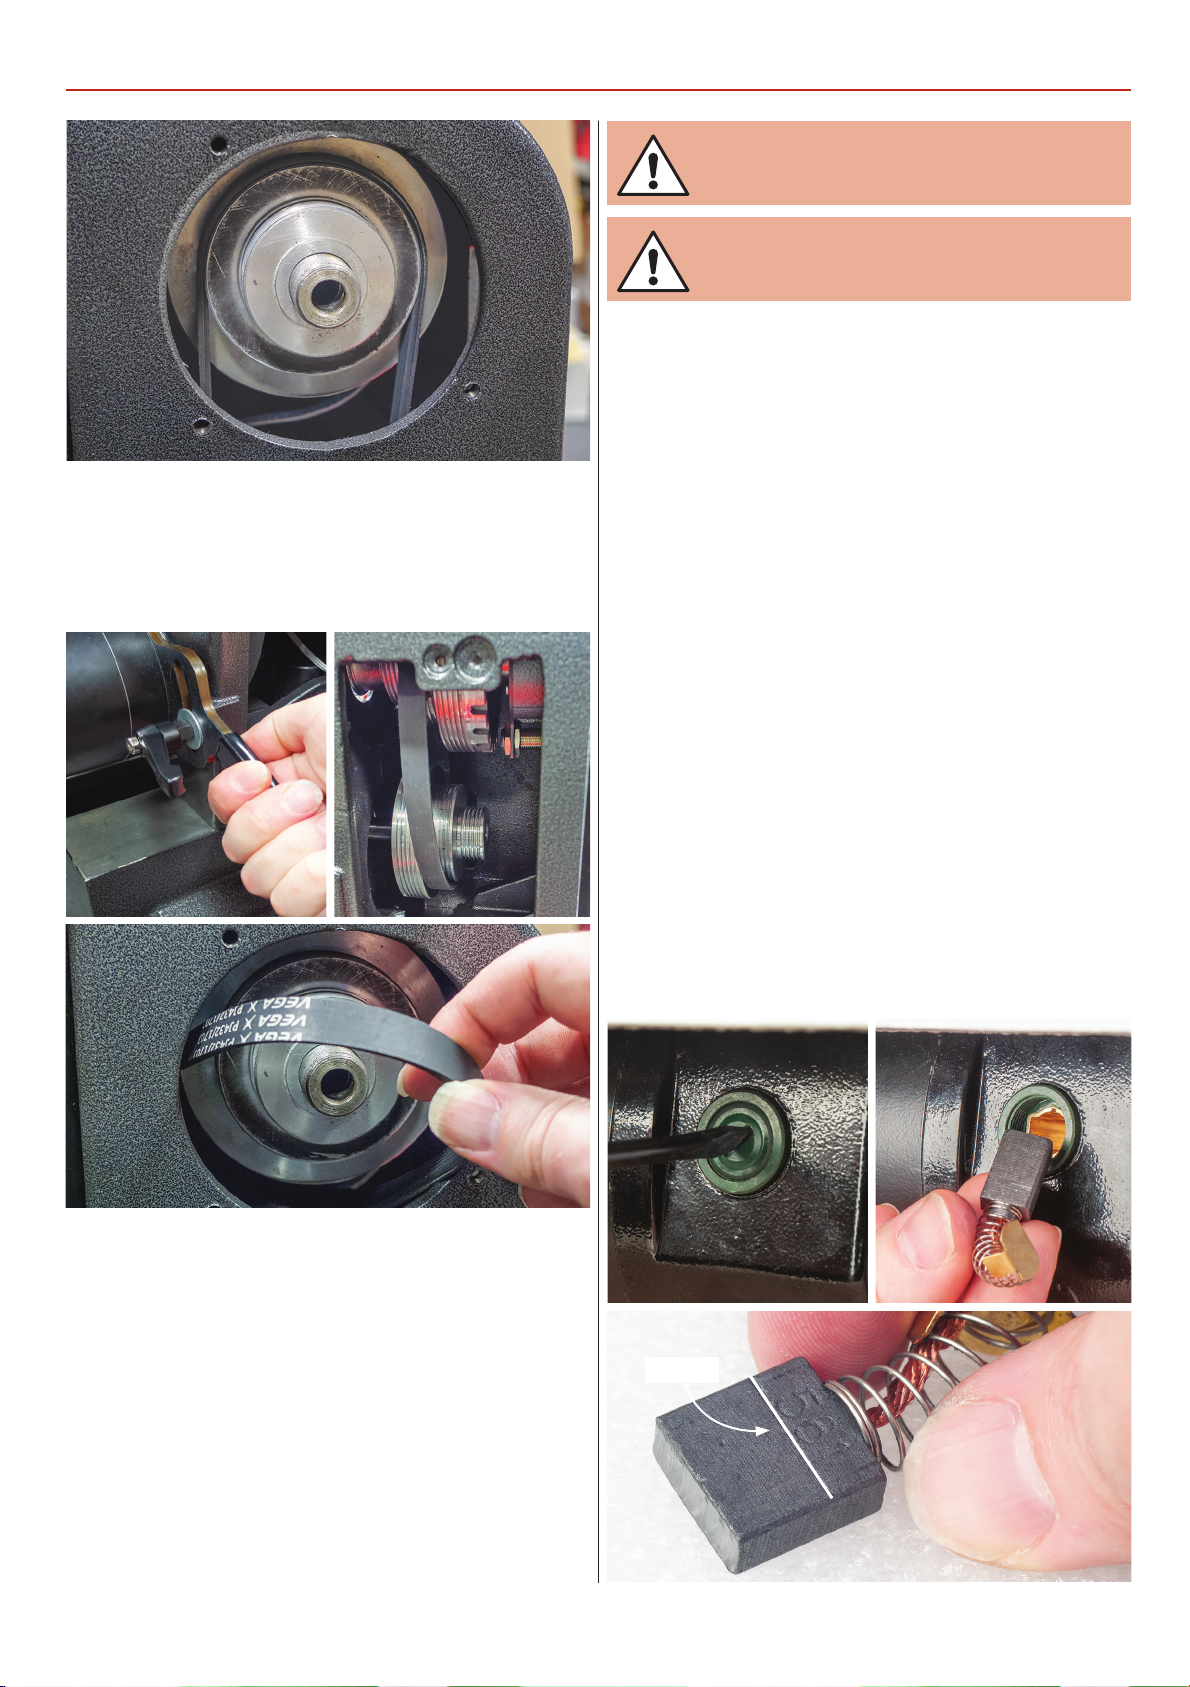
4. Release the tension on the drive belt by raising the
motor assembly, see fig 64. Remove the damaged belt
from the pulleys and out through the spindle access hole,
see fig 65.
Fig 64-65
CAUTION! NEVER START THE LATHE WITH
THE INDEX PIN ENGAGED IN THE SPINDLE.
CONNECT THE LATHE TO THE MAINS SUPPLY!
8. Switch on the lathe and run the machine off load for
several minutes to allow the new belt to bed in. Switch
off the lathe and wait until it comes to a complete stop.
Disconnect the lathe from the mains supply.
Motor Brushes
1. After 100 hours of use, check the condition of the
motor brushes by unscrewing each access port cap in
turn, see fig 66.
NOTE: Take careful note of the orientation of the
brushes, remember that they have bedded themselves
to the profile of the commutator in that position. If you
fit them reversed, it can cause excessive sparking and
heat until they have re-bedded themselves.
2. Remove the motor brushes and check the condition
of the brush head,see fig 67.
5. Check the condition of the new belt, no missing teeth
or splitting for example. Once happy, introduce the belt
back through the access hole as before and fit the new
belt onto the pulleys, making sure the grooves in the belt
mesh into the ones on the drive pulleys.
6. Lower the motor back down to retention the belt,
check that the belt has slight deflection. Tighten
the handle to lock the motor in place, see fig 54-55.
3. If they are in good condition, re-fit. If they were worn
to the ‘Line’ replace with new brushes, see fig 68. For
after sales enquires, call 03332 406406.
4. Replace the new brushes and access port cap screws,
connect to mains supply and run the machine off load
for approximately 20 minutes to bed the new brushes in.
Fig 66-67-68
Line
7. Replace the Faceplate with the three screws,
see fig 62 and reassemble the headstock wheel.
Close the drive pulley door and remove the index
pin (I), unlocking the spindle.
19
Page 20
MAINTENANCE
DISCONNECT THE LATHE FROM THE MAINS
SUPPLY BEFORE CONTINUING!
Daily After Use Monthly
• Clean the wood shavings away from the lathe bed
and tool rest.
• Smear a light coat of wax, ‘Axminster Machine Wax’
or 'camellia oil' over the lathe bed to allow the banjo,
tailstock and headstock to run more smoothly over
the bed. This also prevent corrosion.
• Spray ‘Axcaliber Dry Lubricant’ over the tailstock barrel/
live centre and headstock spindle/chuck after use to
prevents corrosion.
EXPLODED DIAGRAMSLISTS
• Check the tension of the belt and adjust, see page 17-18
for Changing the Belt Speed.
• Check any build up of wood shavings on the motor
and spindle pulleys and clean if necessary.
• Use an ‘M’ class vacuum cleaner to clean the heat sink
air vents on the control switch box assembly.
20
Page 21
EXPLODED DIAGRAMSLISTS
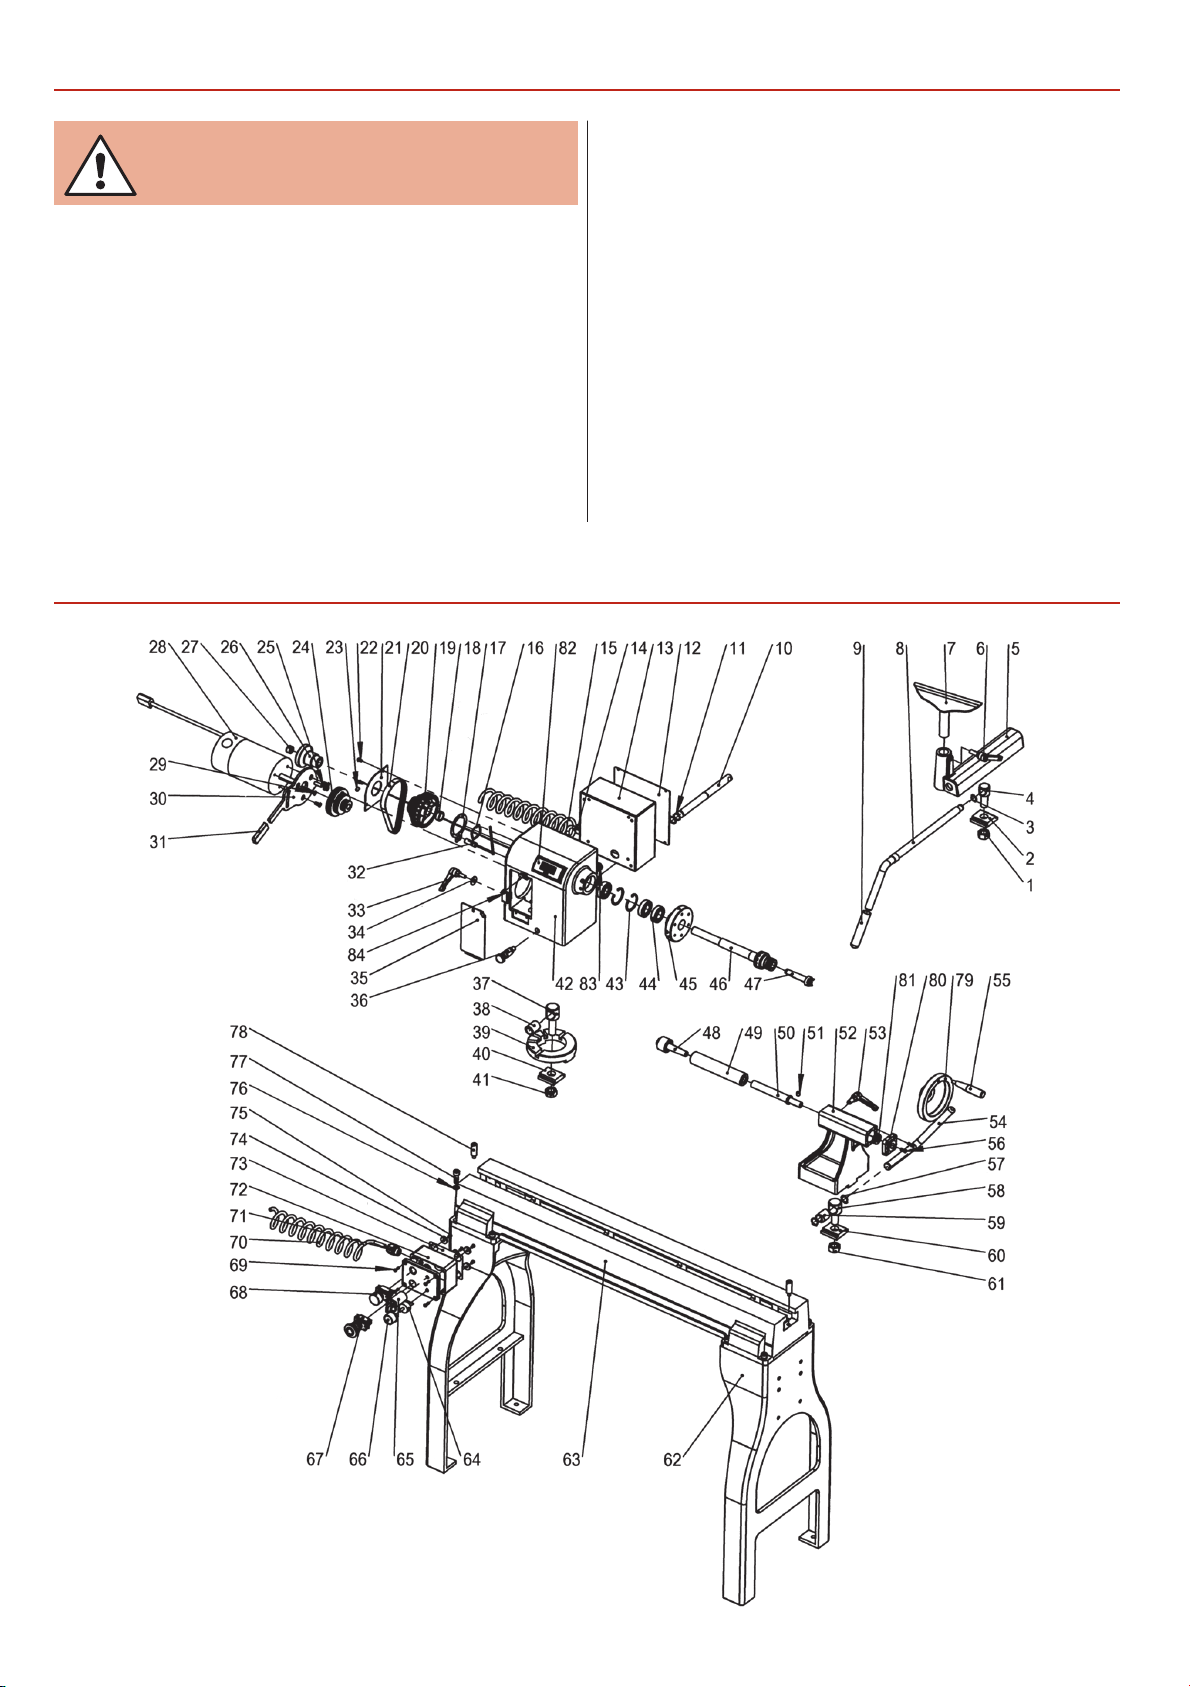
PART No. Description Qty
1 Hex nut 1
2 Fix plate 1
3 Circlip 1
4 Tool rest clamp bolt 2
5 Tool rest base 1
6 Adjustable handle 1
7 Tool rest 1
8 Tool rest base lock lever 1
9 Lock lever sleeve 2
10 Headstock lock lever 1
11 Circlip 2
12 Electrical box cover 1
13 Electrical box 1
14 Stain relief 2
15 Power cord 1
16 Ring 1
17 Bracket 1
18 Sleeve 1
19 Spindle pulley 1
20 Belt 1
21 Spindle pulley cover 1
22 Hex socket screw 7
23 Set screw 4
24 Motor pulley 1
25 Self-locking nut M8 8
26 Spindle wheel 1
27 Locking sleeve 1
28 Motor 1
29 Hex socket screw 4
30 Motor plate 1
31 Handle sleeve 1
32 Digital display components 1
33 Adjusting handle 1
34 large washer 2
35 Headstock door plate 1
36 Angular setting assembly 1
37 Headstock clamp bolt 1
38 Bushing 1
39 Turning base 1
40 Headstock clamp 1
41 Hex nut 1
42 Headstock 1
43 Elastic ring 2
44 Ball bearings 2
45 Faceplate 1
46 Spindle 1
47 Spur center 1
48 Live center 1
49 Quill 1
50 Leadscrew 1
51 Set screw 1
52 Tailstock 1
53 Adjusting handle 1
54 Tailstock locking lever 1
55 Handle for wheel 1
56 Hex socket screw 1
57 Circlip 2
58 Tailstock clamp bolt 2
59 Bushing 1
60 Tailstock clamp 1
61 Hex nut 1
62 Left leg 1
63 Bed 1
64 Potentiometer 1
65 Switch 1
66 Variable speed dial 1
67 ON/OFF Switch 1
68 button (green) 1
69 Screw 16
70 Spiral wire 1
71 Aviationplug 2
72 control box cover 1
73 control box 1
74 Magnet 5
75 Cap screw 5
76 Spring washer 6
77 Hex socket screw 8
78 Bed stop 2
79 Tailstock handwheel 1
80 Tool rest base plate 1
81 Bearing 1
82 PRM digital readout 1
83 Bearing 1
84 Screw 1
21
Page 22
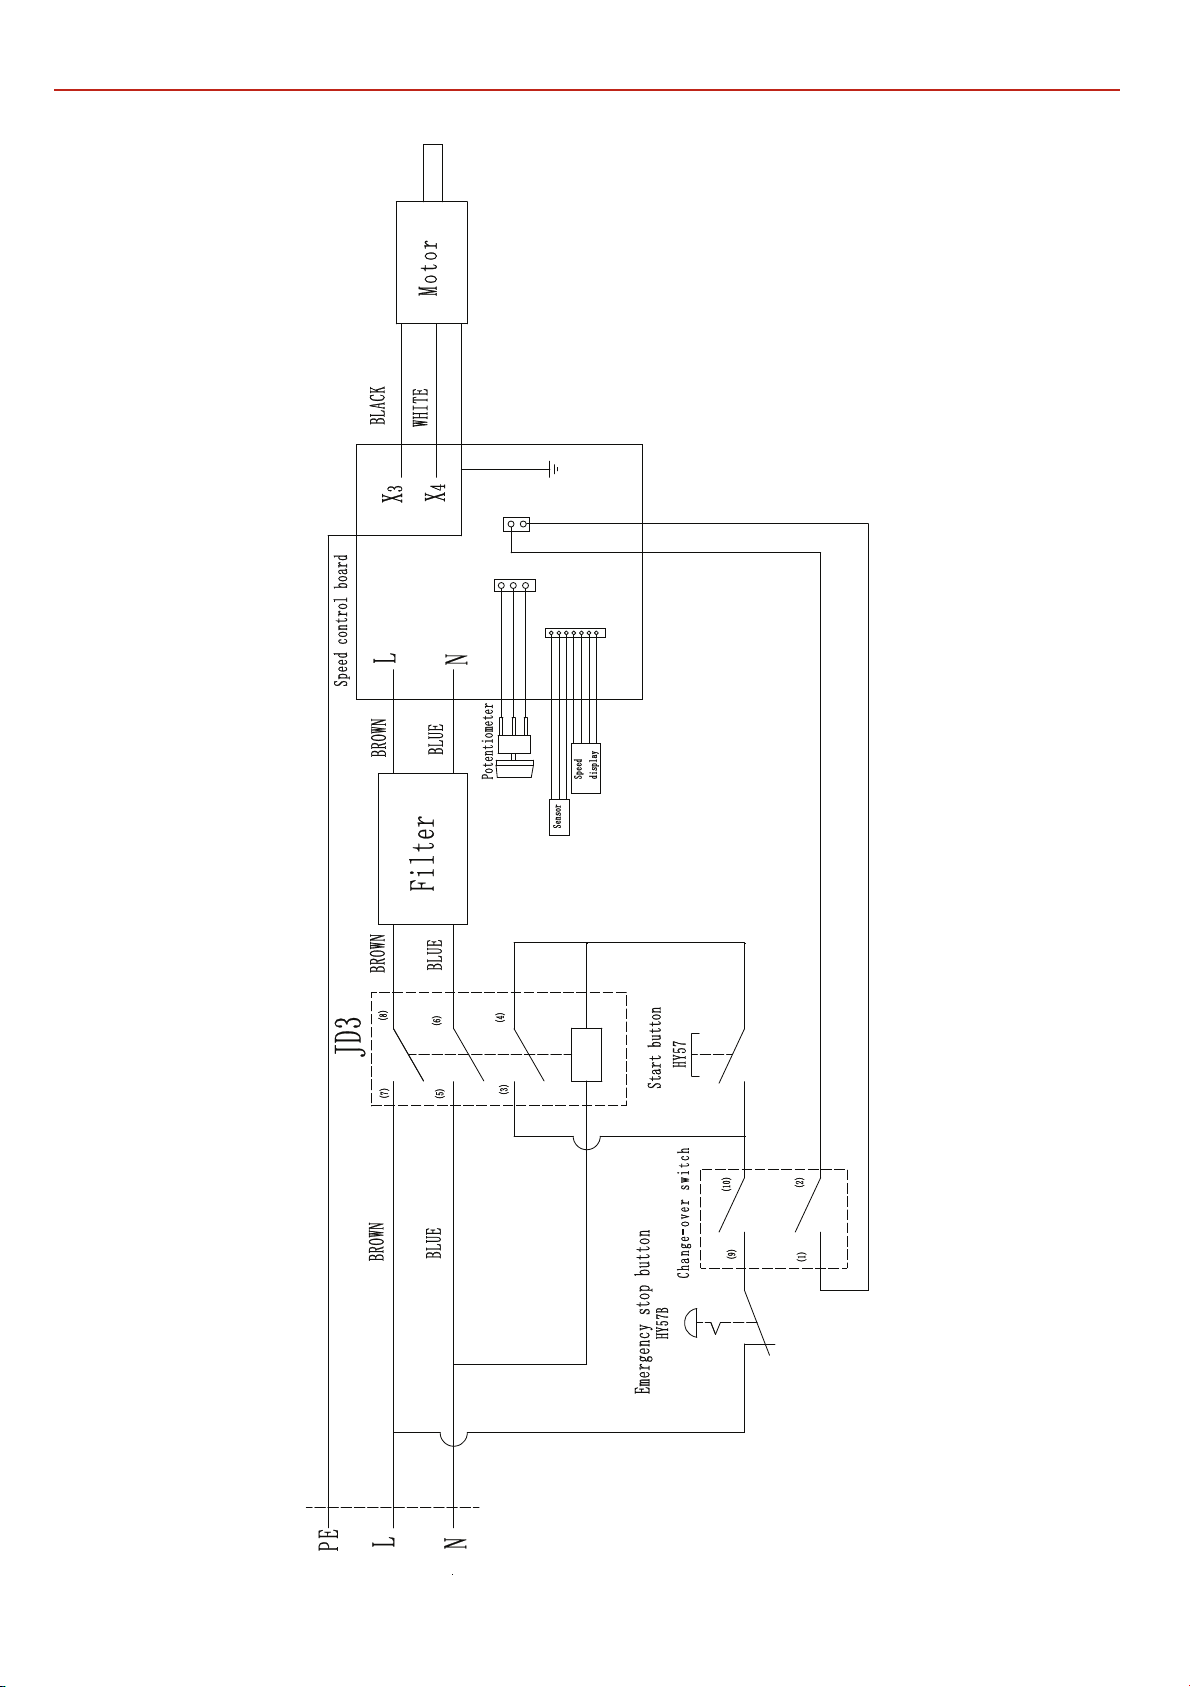
WIRING DIAGRAM
22
Page 23
Page 24
The packaging is suitable for recycling.
Please dispose of it in a responsible manner.
EU Countries Only
Do not dispose of electric tools together with household waste material.
By law they must be collected and recycled separately.
Axminster Tools, Axminster Devon EX13 5PH
axminstertools.com
 Loading...