

Page 1
More Information...General Assembly...
Axminster. Devon. EX13 5PH. UK
FREEPHONE 0800 371822
4
If you are still a little unsure about getting into pen
and project kit making, why not come on one of
our one day courses here at Axminster.
This is a one day course for anyone who wants to
learn the art of pen making and producing objet
d’art from project kits. If you are thinking of buying a small
lathe or have a lathe, this is the course for you. Gaining a real insight into what
can be achieved, after one day you will be able to leave with the completed,
professionally finished masterpieces and a multitude of ideas and skills.
For details visit: www.axminsterskillcentre.co.uk
or call: Vicky Turner on 0800 9751905.
online
VIDEO
!
available
Pen Kits The Principles of Turning
www.axminster.co.uk/penmaking
Pen Kit
Instructions
10 & 24ct Twist Pen
Order No: 340075 & 310490
www.axminster.co.uk/penmaking
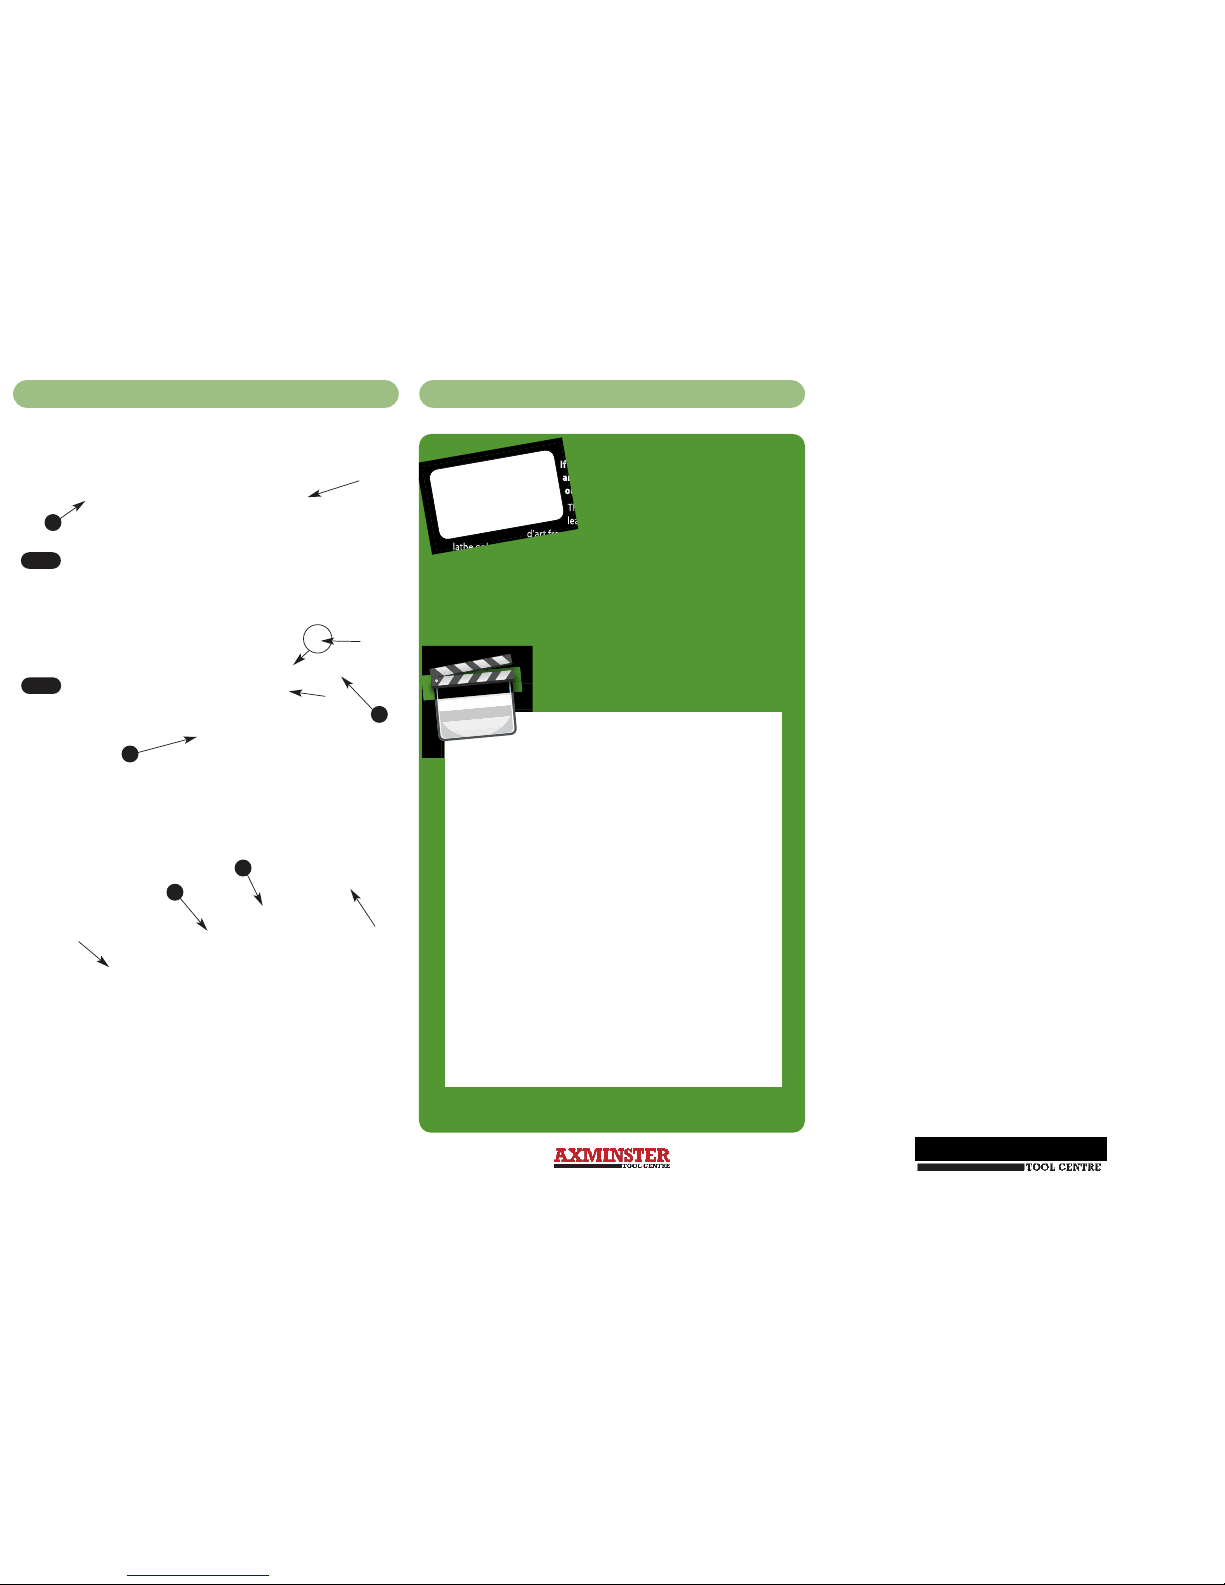
Carefully align the Pen Tip (f) with the lower end of the lower body, press firmly
together. (See Fig 7).
e
Lower body
Groove
Fig 7
Align the twist mechanism (e) with the upper end of the lower body, with the brass
end first. Firmly press the twist mechanism (e)into the body as far as the groove.
See Fig 8. Introduce the Pen refill (g) into the twist mechanism and screw it ‘home’.
b
g
g
Add the centre band (b) and carefully align and press the upper pen body over the
end of the refill (g) and over the twist mechanism. See Fig 9. There is sufficient grip
between the upper pen body and the twist mechanism to keep the upper body in
place and to enable the mechanism to be twisted to extend and retract the ball
point.
Fig 8
Upper body.
Lower body
f
Page 2
1
23
Instructions for 10 & 24ct Twist Pen Kits...
Preparing the Bodies...
Turning the Bodies...
Kit No. 340075 10ct Twist Pen Kit
Kit No. 310490 24ct Twist Pen Kit
Pictures of samples of the finished articles, in both timber and acrylic, can be found in
our catalogue in the ‘Woodturning Projects’ Section.
Below is a list of the items required to make the finished items from the purchased
kits (Not including the body blanks). If you do not possess these items we have
offered our catalogue stock code numbers alongside the items as a quick guide. We
have tried to include everything in the list, although we realise that many
woodturners will already have most of them.
Required items...
E
y
e
P
r
o
t
e
c
t
i
o
n
E
a
r
D
e
f
e
n
d
e
r
s
D
u
s
t
M
a
s
k
Alternatives are listed to cater for different lathe configurations.
Order No:
Deluxe Pen Mandrel 1MT 211322
Deluxe Pen Mandrel 2MT 211323
60˚ Live Tail Stock Centre 1MT 340202
60˚ Live Tail Stock Centre 2MT 340203
60˚ Live Tail Stock Centre 3MT 340204
7mm Drill Bit (we recommend the Colt Pen Drill) 702554
Axminster Universal Barrel Trimmer 700265
2 Part Rapid Epoxy Resin Adhesive 340282
Alternative Zap-A-Gap Adhesive (Cyanoacrylate) 990095
Recommended Accessories...
Quick Action Pen Blank Vice 600771
Pen Blank Sizing and Cutting Jig 600623
Axminster Pen Assembly Press 200205
What’s in the Kit...
2 Brass Tubes (52.5mm Long)
1 Centre Band
1 Pen Clip Retainer Cap
1 Pen Clip
1 Twist Pen Mechanism
1 Pen Tip
1 Pen Refill
(a)
(b)
(c)
(d)
(e)
(f)
(g)
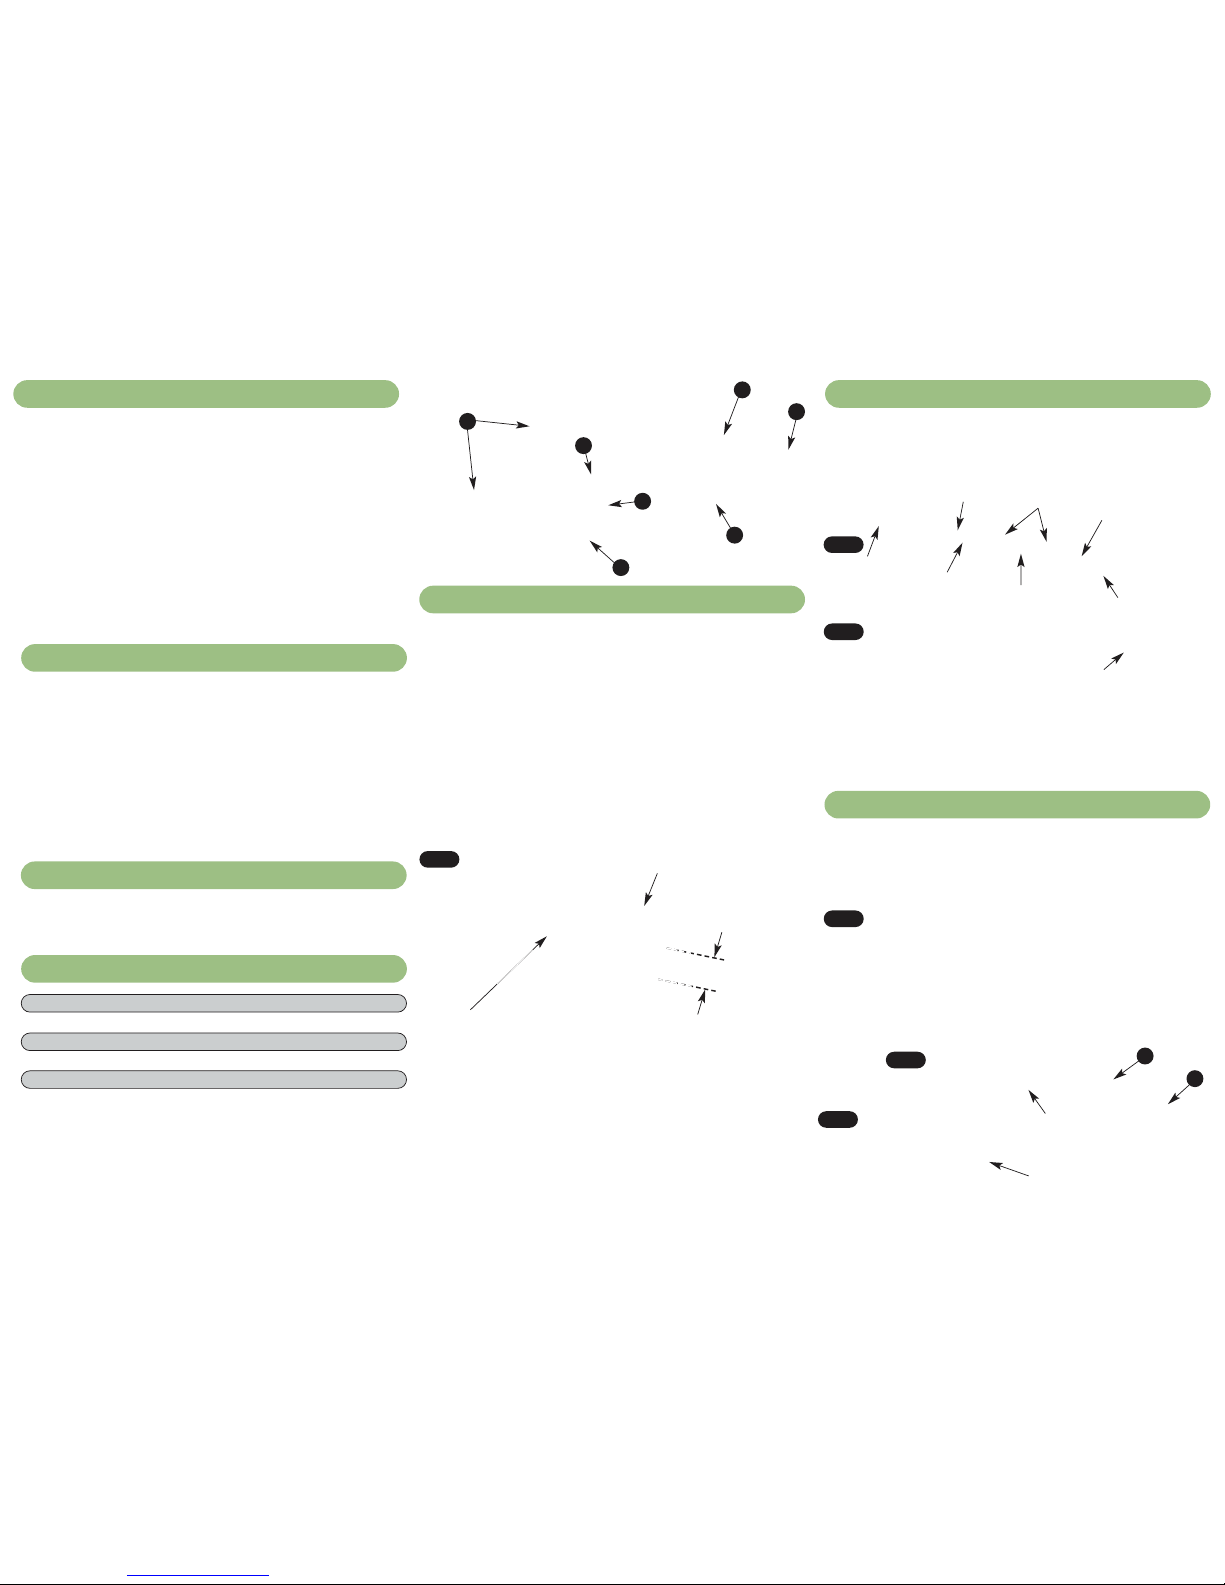
Using 16mm (5/8”) Square stock; cut the blanks to the length of the brass tubes
adding 2-3mm to allow for trimming. The Pen Blank Sizing and Cutting Jig makes this
process very much easier.
Drill a 7mm diameter hole through the centre of each blank. Care must be taken not
to force the drill bit, (this may cause it to ‘wander’ from the centre line), and
remember to back out the drill frequently to clear the debris from the hole. If you are
using a pillar drill the Quick Action Pen Blank Vice is a very useful accessory for this
task, it ensures that the blank is held upright and firmly in position. Moreover, if the
vice is clamped to the table of the drill, it will provide accurate repeatability for all the
blanks that require drilling.
When the holes are drilled, spread the adhesive randomly over the brass tubes and
insert the tubes into the blanks using a twisting motion to ensure the glue is spread
evenly between the two surfaces. Over insert the tubes into the blanks by
approximately 1mm giving an allowance for the blank to be trimmed to size and the
excess glue to be removed. (See Fig 1).
a
b
e
f
g
c
d
Zap Z-7
Debonder
Blank
Brass tube
7mm
ø
Warning. If you are using cyanoacrylate adhesive, exercise extreme caution and
do not allow the adhesive to come into contact with the skin. If this happens
keep the affected area from contact with any other surface, until the glue has
hardened or you can treat the area with a softening agent similar to Zap Z-7
Debonder (990099), and you can remove the glue.
Allow the adhesive to dry thoroughly.
Using the Barrel Trimmer trim the ends of the blanks squarely and neatly to the ends
of the brass tubes; this will also remove any excess glue that may have exuded from
the joint. Take care not to undercut the brass tubes.
Slide an end mandrel spacer bush onto the shaft. Assemble the two tubed blanks
onto the mandrel with a spacer bush in between; add the last end spacer bush and
the locking nut. Tighten the locking nut to allow the assembly to be turned without
‘creeping’. Do not overtighten, this may cause the assembly to distort, the bodies to
split, strip the thread on the lock nut, etc. Mount the complete assembly onto your
lathe (See Fig 2).
Fig 1
Morse taper shaft
Mandrel bush
Blanks
Bushing
Bushing
Bushing
Locking nut
Live tail stock centre
Do not advance the tailstock centre with too much force. The current bulk of the
blanks may be adding strength to the assembly but as the body diameters are
reduced, too much force on the mandrel may cause it to distort or bow.
Turn the blanks to your preferred profiles, sand and finish as required to the
diameters of the spacer bushes. (See Fig 3). If you have turned dissimilar profiles on
the bodies, it is sensible to identify them somehow e.g. upper and lower body.
Remove the finished bodies from the pen mandrel.
Fig 2
Fig 3
General Assembly...
Axminster Pen Assembly Press
Fig 4
Note. The Axminster Pen Assembly Press (200205) is a very useful accessory for
these operations, as it gives greater control over the applied force and keeps
the components in line (See Fig 4).
Locate the Clip (d) and the Retainer Cap (c). Ensure they are carefully aligned (See
Fig 5). Press the Clip Retainer (c) through the Clip (d) itself into the ‘upper’ end of
the ‘upper’ body. (See Fig 6).
Fig 5
Fig 6
c
d
Upper body.
Continues Over....
 Loading...