

Page 1
... print your plane | www.3DLabPrint.com
User Guide
rev. 2021/12
Fully 3d printable
Mitsubishi A6M2 Zero
scale 1:12, wingspan 1000 mm / 39.4 inch
page 1
Page 2
... print your plane | www.3DLabPrint.com
A6M2 Zero
fully printable R/C plane for your desktop 3Dprinter
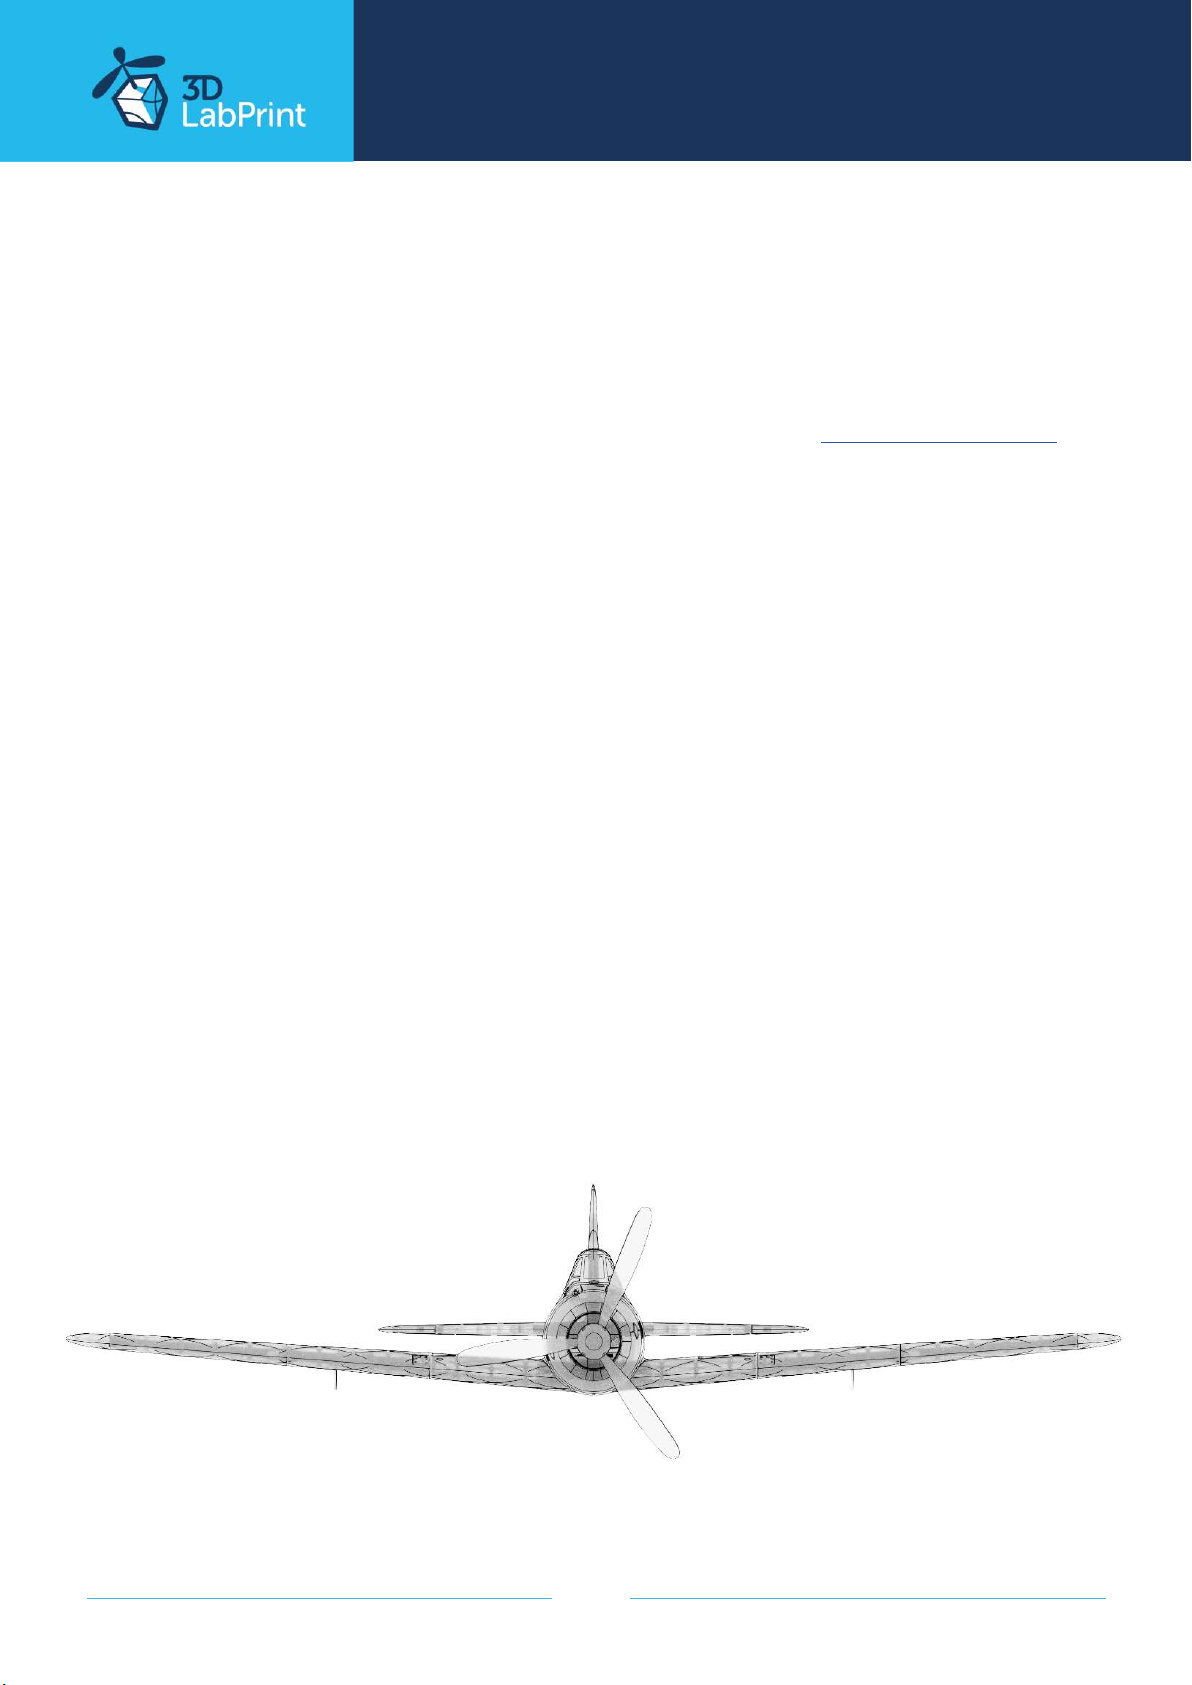
Fully 3D printable RC model of the Japanese attack plane, specially designed to meet ACES
and EPA aircombat requirements, but also as a cheap and easy to build RC model for everyday flying. Many scale details such as armament or airframe plating encourages to create
realistic paint jobs. This plane has been designed for printing from PolyLight 1.0 LW-PLA ac-
tive foaming filament, that allow even the small printed planes to be as light as any other RC
plane building technique. Get ready for battle with this great performing flying legend!
The first fully printable airplane files prepared for your 3Dprinter, with
flight characteristics, comparable or even supperior to classic build model airplane.
This is not a dream, now you can print this HI-TECH at home. Simply download and print
the whole plane or spare parts anytime you need just for a cost of filament only about $12
Extensive hi-tech 3d structural reinforcement making the model very
rigid while maintaining a lightweight airframe and exact airfoil even it’s just a plastic. This
perfect and exact 3d structure is possible only thanks to additive 3dprinting technology. So
welcome to the 21st century of model flying and be the first at your airfield.
Easy to assembly, you don’t need any extra tools or hardware, just glue printed
parts together and make pushrods for control surfaces. The rest of the assembly is very
easy. Simply add brushless motor, ESC, servos and radio system. Don’t worry, detailed step
by step PDF/VIDEO is included.
You’ll get a superb performing airplane with highly ecient powerplant capable of flying 7+
minutes at full throttle and speeds exceeding 80 kph. Low stall speed is achieved for easy
landing on the other hand.
page 2
Page 3
... print your plane | www.3DLabPrint.com
General specifications (HP setup):
Wingspan: 1000 mm / 39.4 inch
Lenght: 726 mm / 28.5 inch
Height: 188 mm / 7.4 inch
Wing area: 18,3 dm2 / 1.96 square feet
Wing loading: 31 g/dm2 / 15.3 oz/square feet
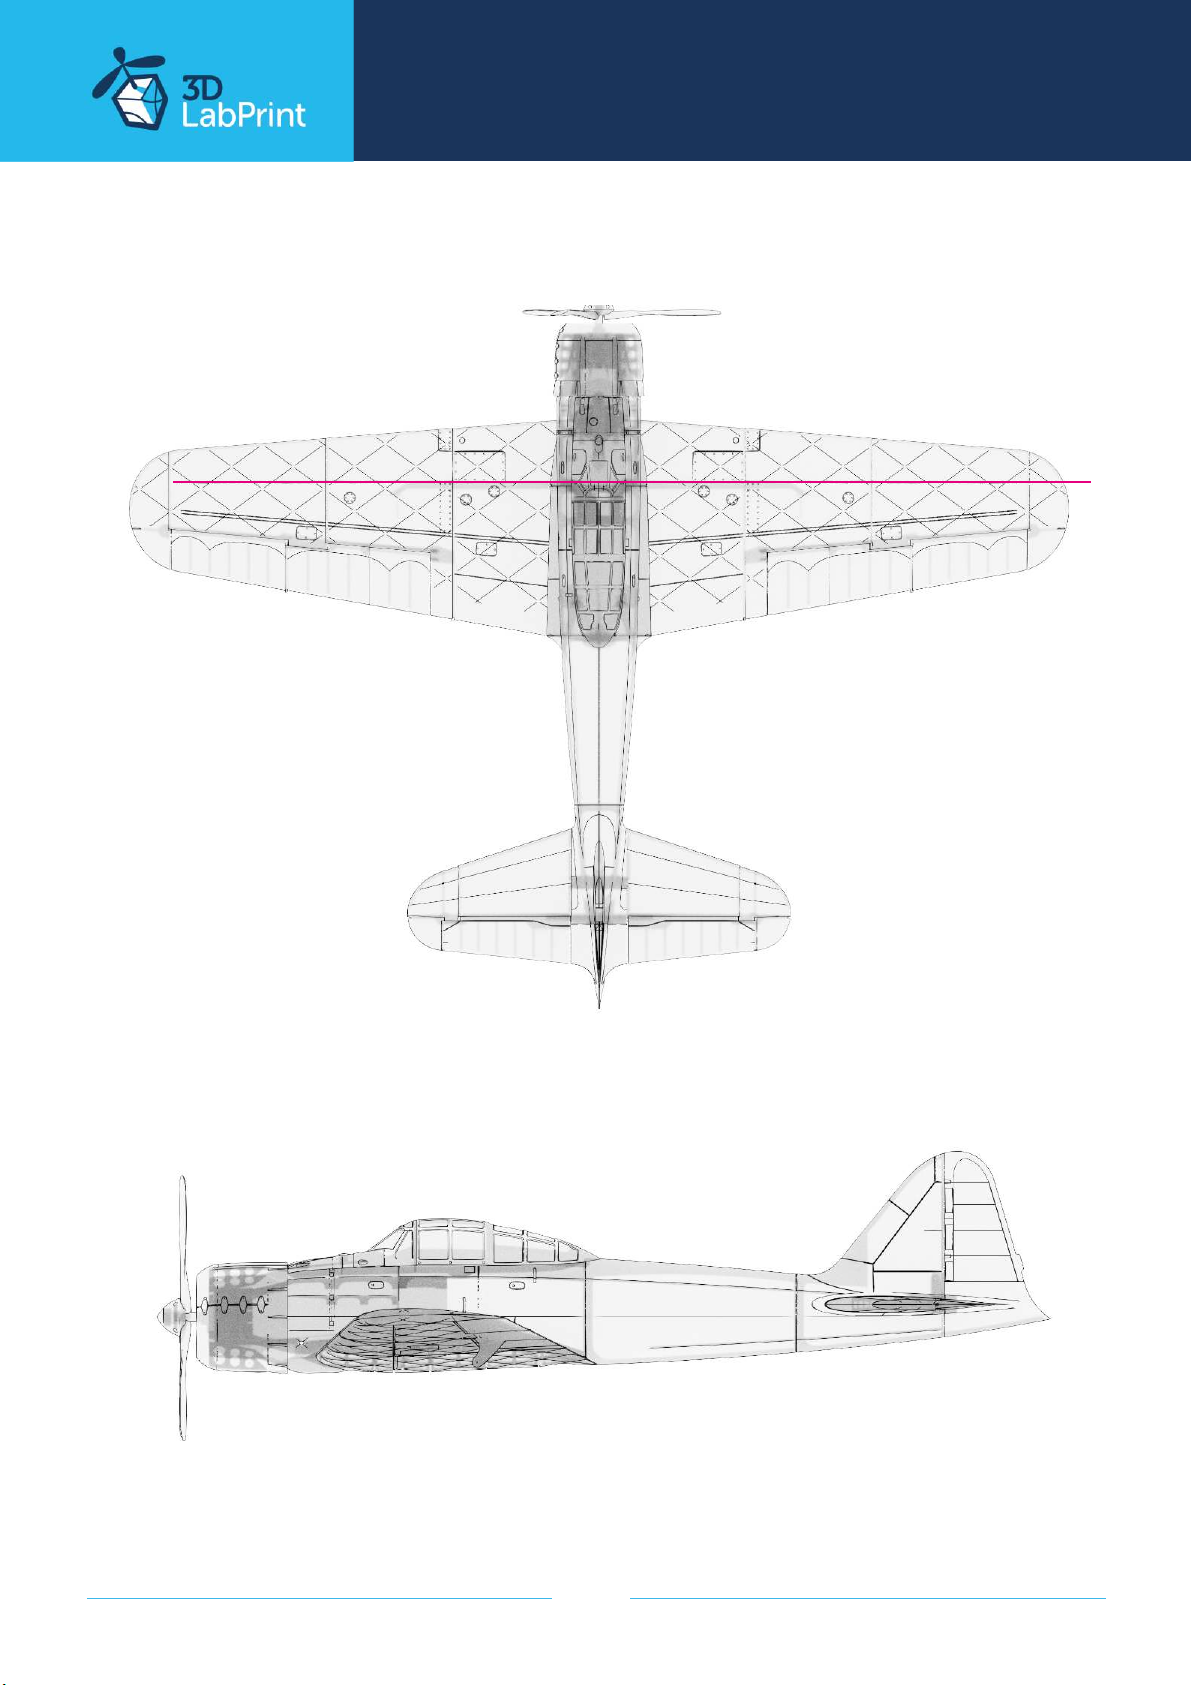
Center of gravity: at the wing spar (60 mm from the leading edge)
Airfoil: LHK508 modified by 3DLabPrint
Print weight (LW PLA): 224 g / 7.90 oz
Empty weight (w/o battery): 380 g / 13.40 oz
Takeo weight (3s 1300 lipo): 500 g / 17.63 oz
Max takeo weight: 700 g / 24.70 oz
Never exceed speed, VNE: 110 km/h / 62 mph
Design maneuvering speed, VA: 50 km/h / 31 mph
Stall speed, VS: 15 km/h / 9.4 mph
Recommended setup
Motor: Leopard LC2830 980KV (for 3-4S setup)
ESC: 20A/3-4S
Propeller: two blade GWS 9 x 7,5 (ugly orange)
Battery: 1500/4S
printed PET motor mount
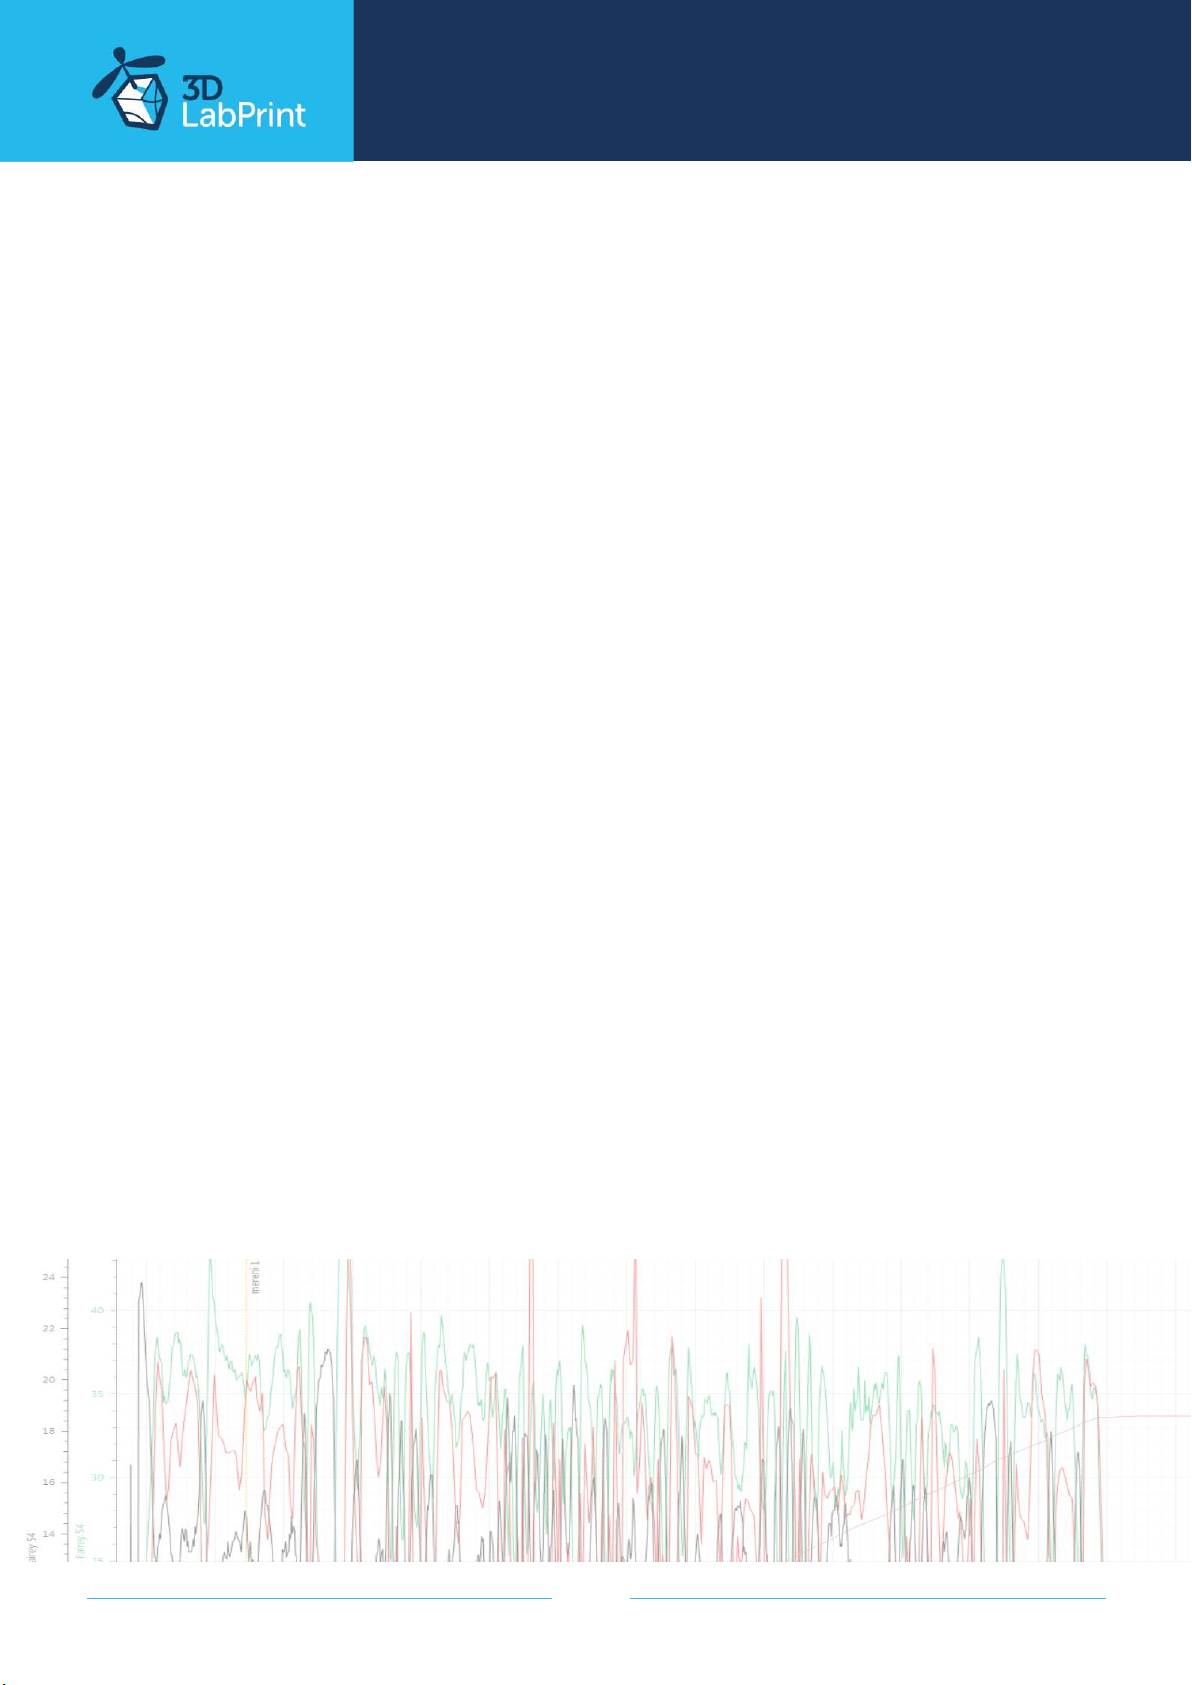
Performance measurement
Max speed VH (level flight): 105 km/h – 56.7kn – 65.2mph with GWS 9x7,5
Rate of climb: 20 m/s (5 373 ft/min) with GWS 9x7,5
Flight time (3s 1300mAh/full): 7:30 with GWS 9x7,5
page 3
Page 4
... print your plane | www.3DLabPrint.com
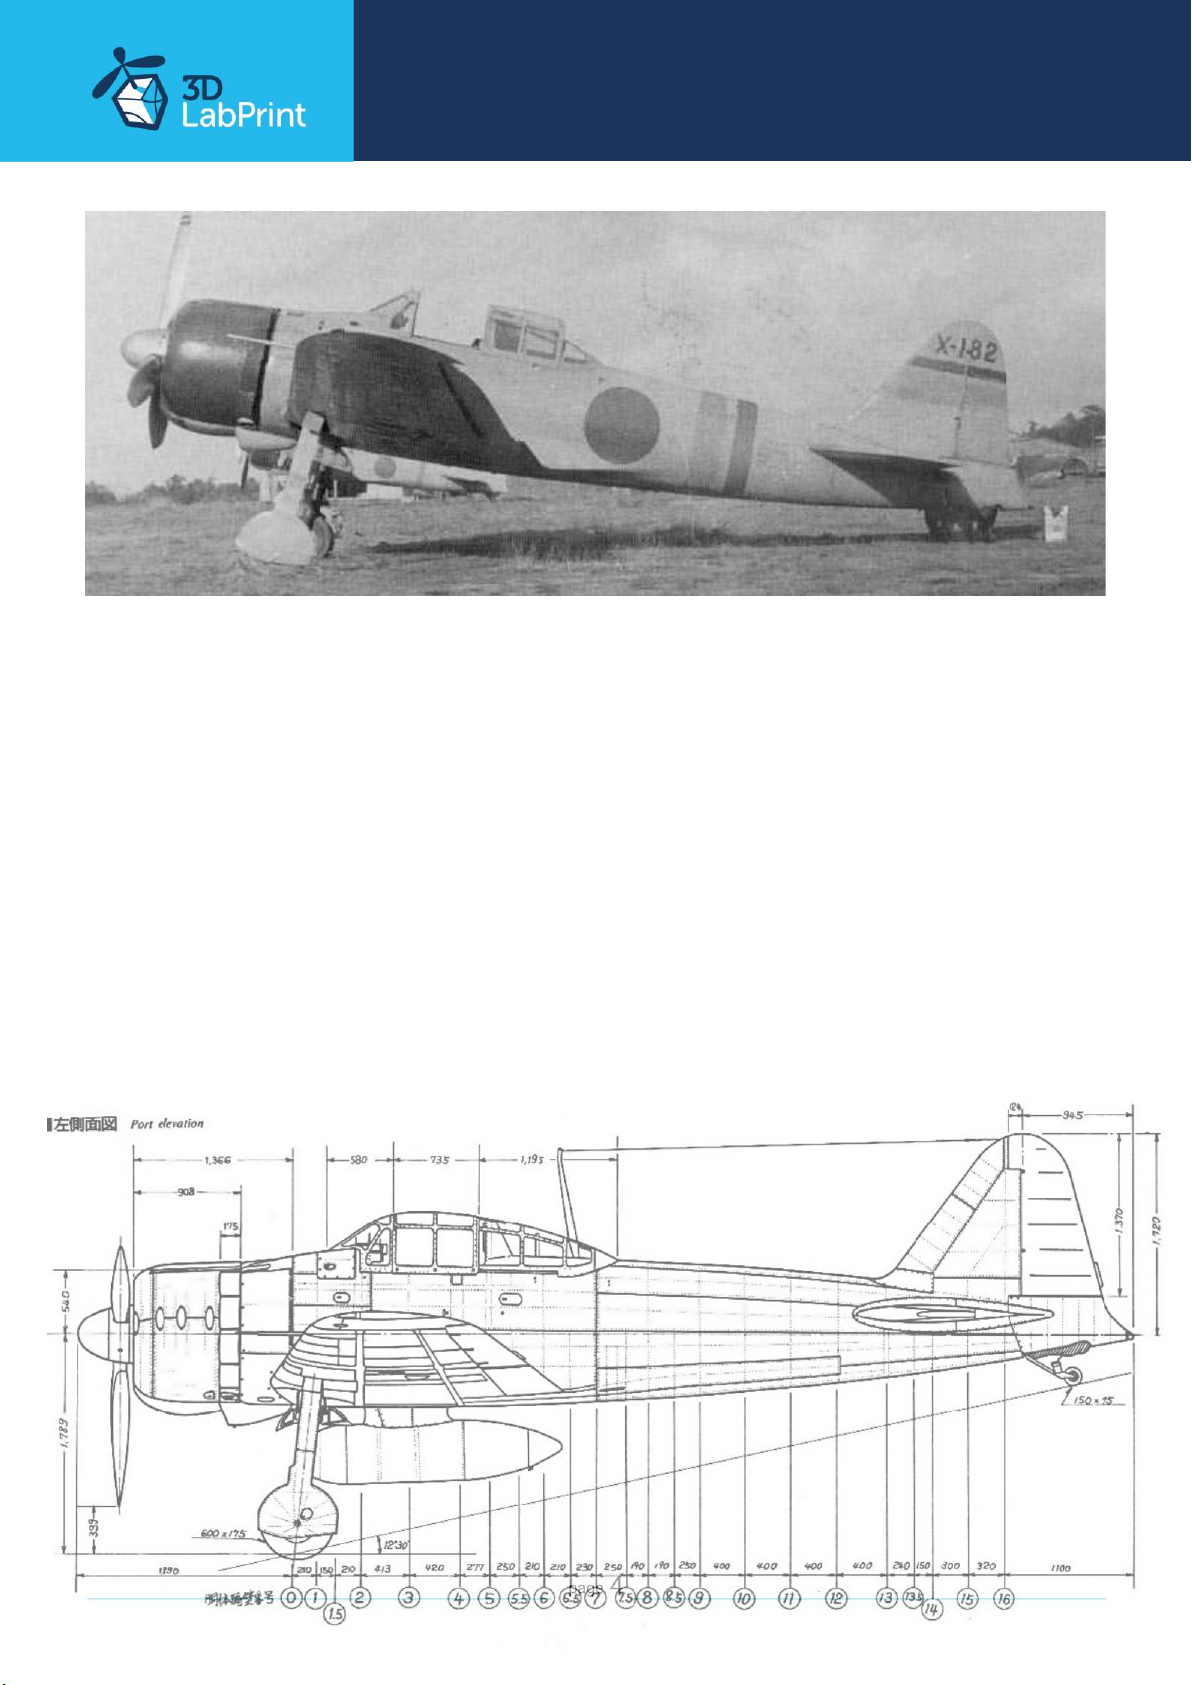
Mitsubishi A6M2 Zero (rei-shiki-kanjō-sentōki), History
The Mitsubishi A6M „Zero“ was a long-range carrier-based fighter aircraft formerly
manufactured by Mitsubishi Aircraft Company, a part of Mitsubishi Heavy Industries, and
operated by the Imperial Japanese Navy from 1940 to 1945. The A6M was designated as the
Mitsubishi Navy Type 0 carrier fighter.
The Zero is considered to have been the most capable carrier-based fighter in the world
when it was introduced early in World War II, combining excellent maneuverability and very
long range. The Imperial Japanese Navy Air Service also frequently used it as a land-based
fighter.
In early combat operations, the Zero gained a reputation as a dogfighter,[3] achieving an
outstanding kill ratio of 12 to 1, but by mid-1942 a combination of new tactics and the
introduction of better equipment enabled Allied pilots to engage the Zero on generally equal
terms. During the final phases WWII, it was also adapted for use in kamikaze operations.
Japan produced more Zeros than any other model of combat aircraft during the war.
page 4
Page 5
... print your plane | www.3DLabPrint.com
Included:
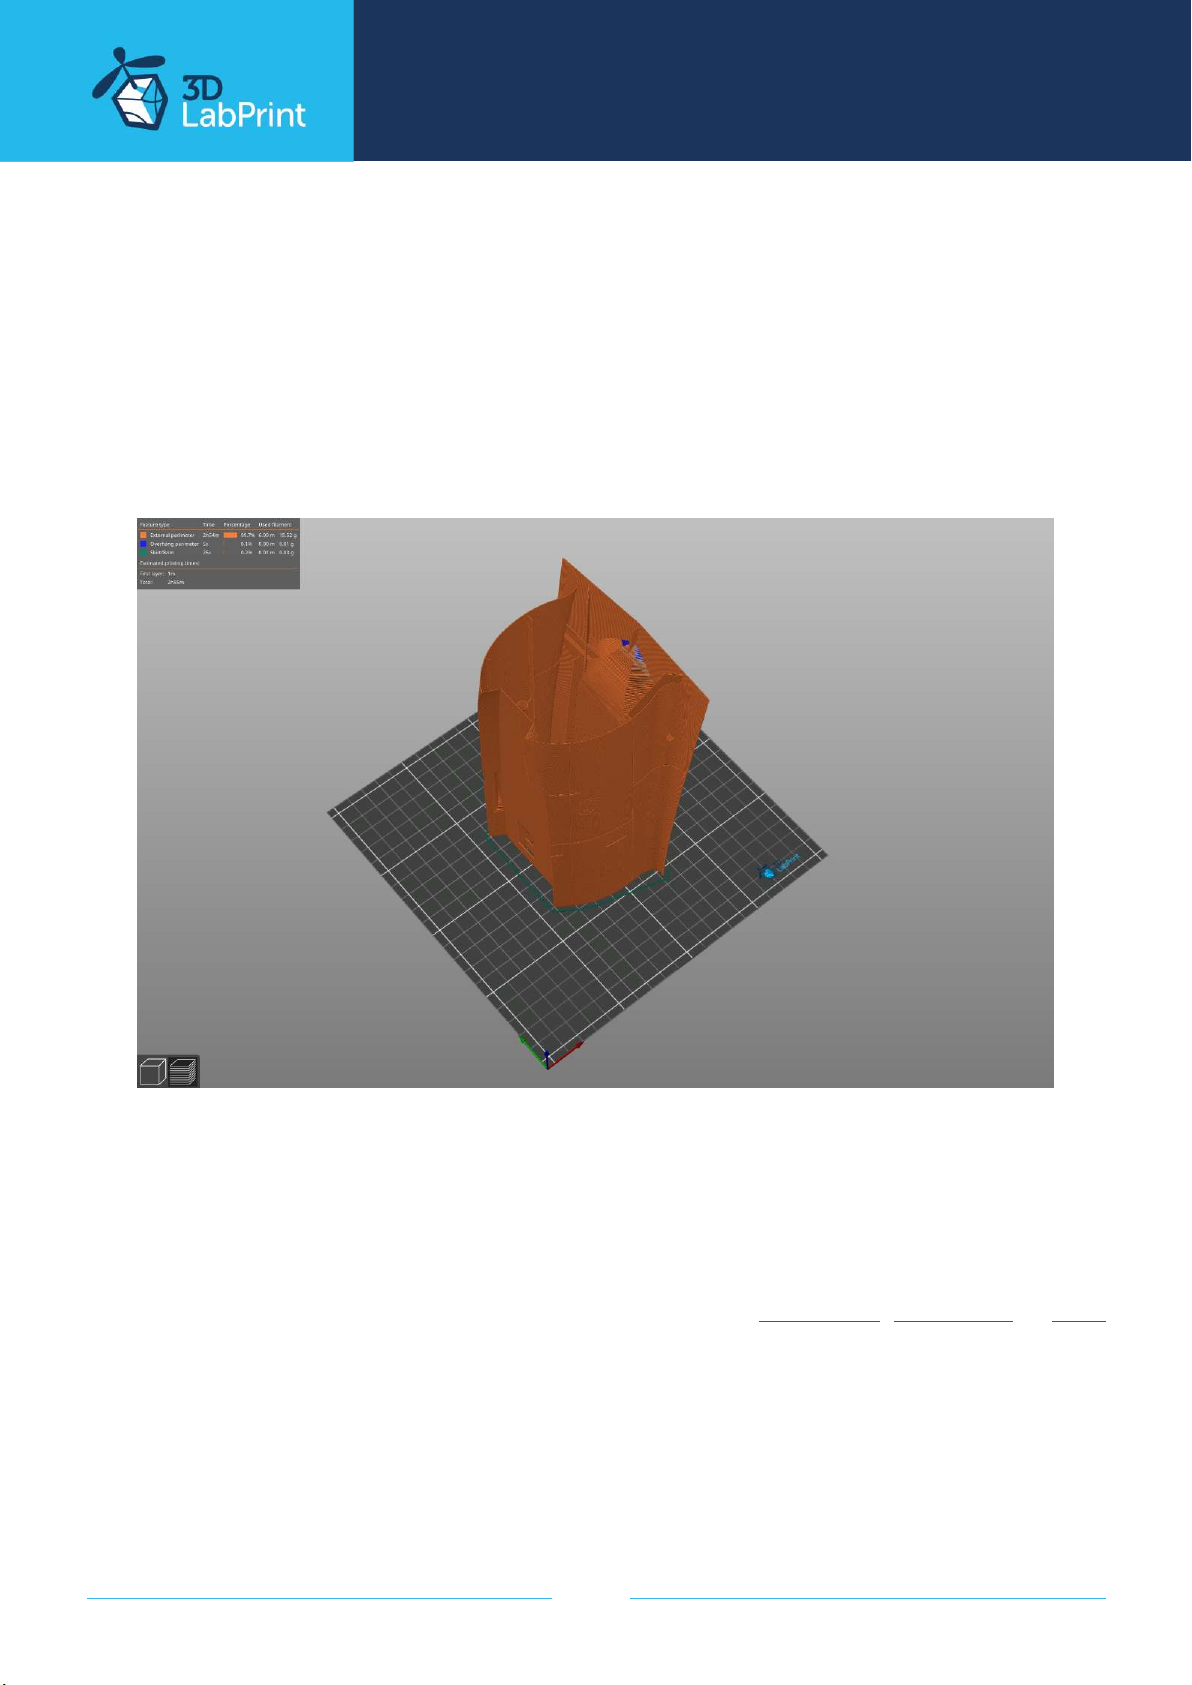
1. 3MF 3D files (primary)
Used instead of STL files
3mf files can be used instead of standard STL files, but also include information about slicing
in the new version of Prusa Slicer (since version 2.4). Open them directly in the Prusa Slicer
as a project or import to the slicer of your choice. The files contain settings for printing on a
direct drive printer with dimensions 200x200x200 mm, that can be further adapted to suit
your printer. The generic settings are compatible with Prusa MK2/3/3S printers.
2. Factory files for Simplify3D slicer
contains all the necessary settings to slice the models along with suggested bed layout. We‘re
using PRUSA i3 ORIGINAL printers so you may need to adjust the basic printing parameters
to match your printer or use these files as a start point for you.
3. Printing Guide in our Help Section
Apart from this userguide, please see the Printing Guide for PrusaSlicer, Simplify3D or Cura
to find some Tips and Advice for airplane printing (Thin Wall Printing).Remember: We use 0
retraction and 0.4-0.5 flow with LW-PLA.
4. Gcodes
Basic Gcodes prepared for direct use, as universal as possible. Should work on i3 style
printers, Give it a try, but we can‘t guarantee it will work on your printer. Wall thickness
should be 0.60-0.67mm.
page 5
Page 6
... print your plane | www.3DLabPrint.com
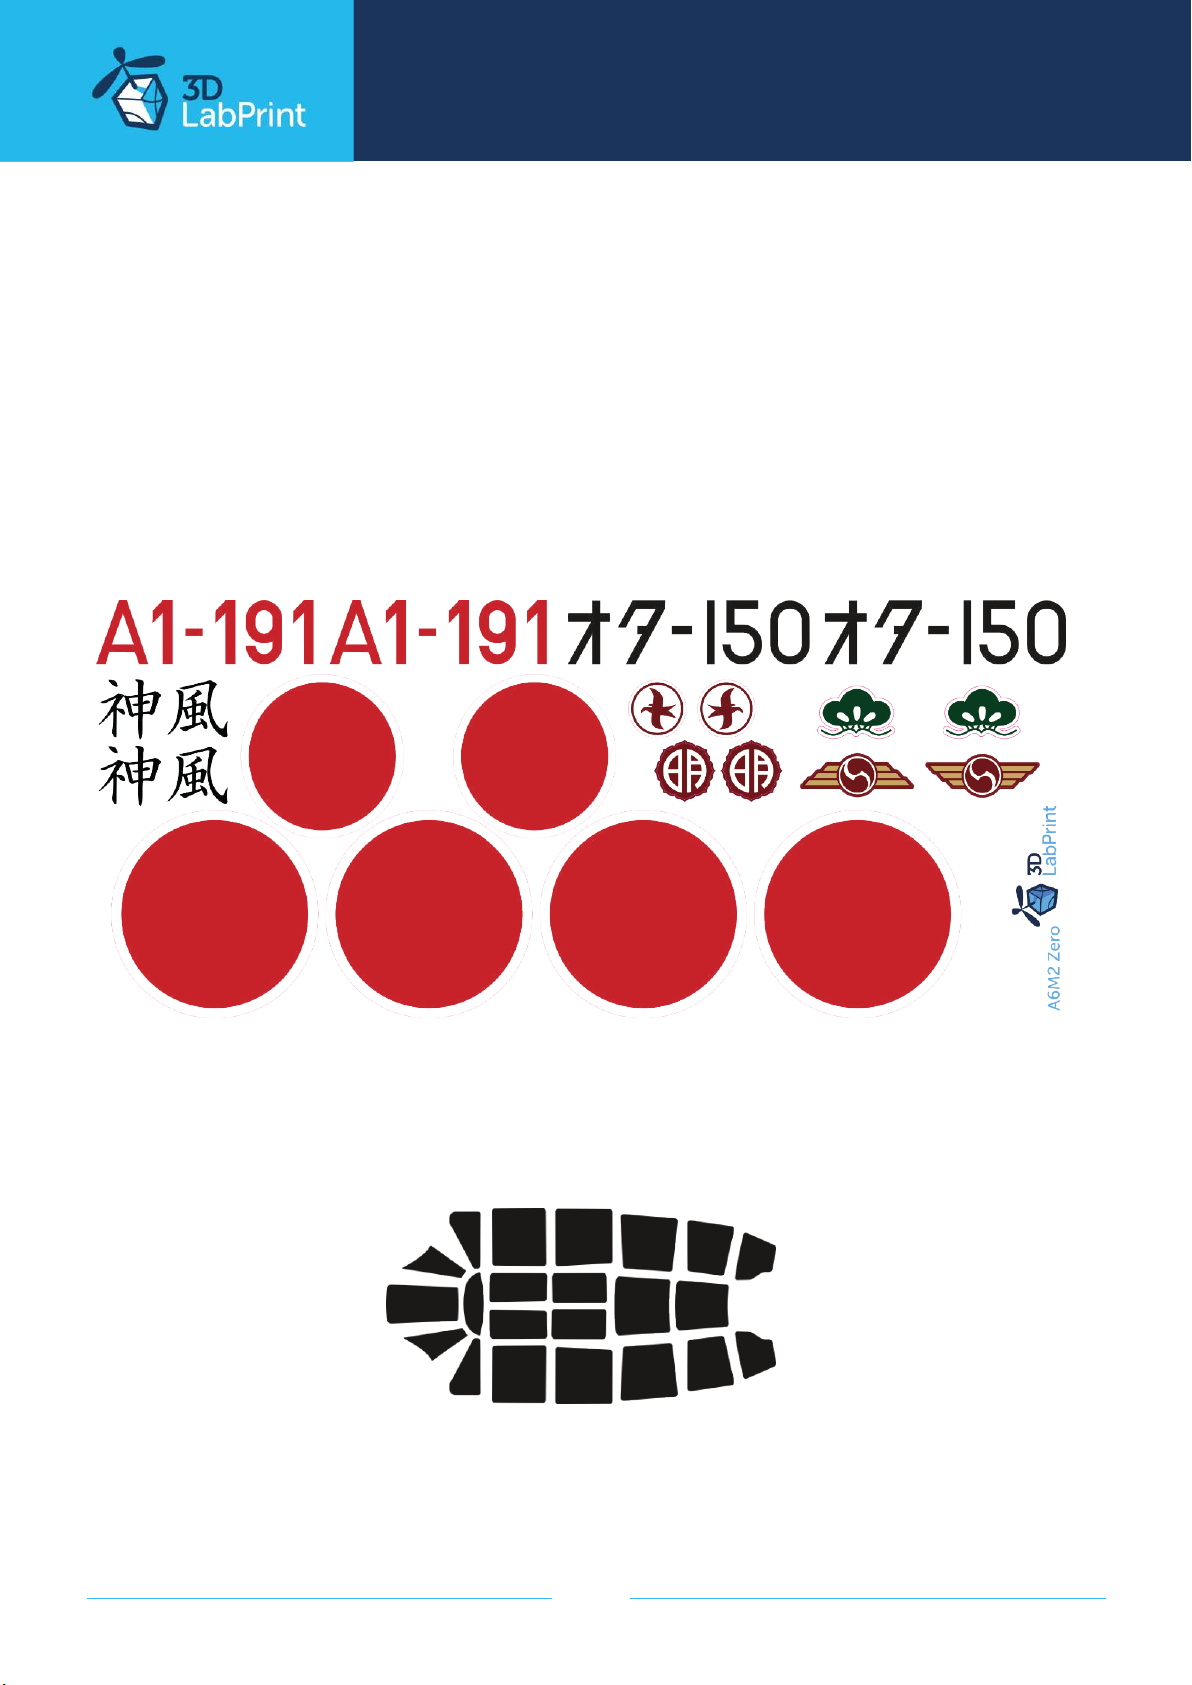
5. Scale markings PDF
You could print and cut the PDF in scale from thin self adhesive advertisement foil and place
it on the model as needed.
page 6
Page 7
A6M2 Zero
... print your plane | www.3DLabPrint.com
Centre of Gravity
Wing area: 18,3 dm2 / 1.96 square feet
Lenght: 726 mm / 28.5 inch
page 7
Page 8
... print your plane | www.3DLabPrint.com
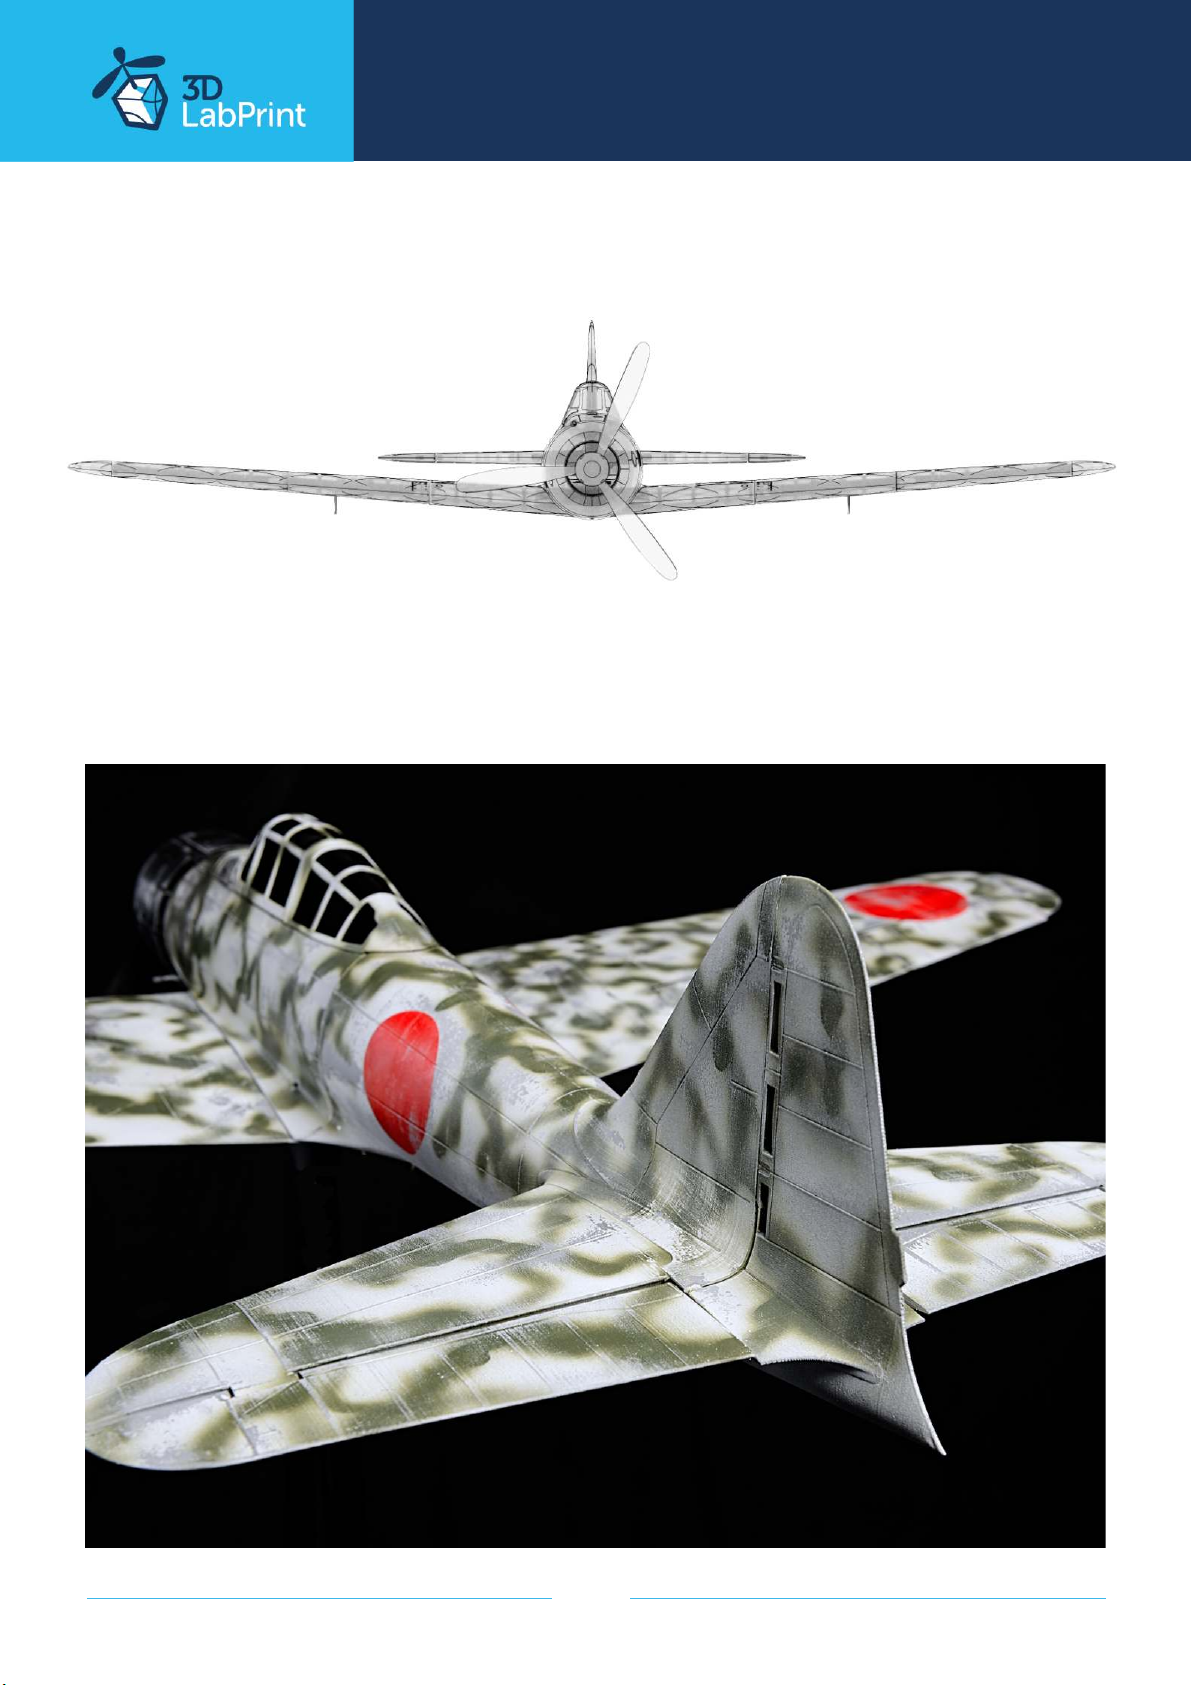
Wing span: 1000 mm / 39.4 inch
page 8
Page 9
... print your plane | www.3DLabPrint.com
Step By Step PDF/VIDEO userguide
1. Choose airplane at www.3Dlabprint.com, visit our Facebook for latest info.
Basic requirments for A6M2 Zero are 200/200/195 mm
volume, nozzle 0.4mm recommended (0.35 or 0.5mm
alternativelly). Heated bed recommended. Designed to be
printed with Polylight LW-PLA filament by 3DLabPrint.
Contact: [email protected]
2. Create account, download
You will receive download link to all the zipped files to your
email right after the checkout (please check your spam folder
if not). If you are logged in with your account while purchasing
the model, you will find the download link in your account’s
Downloads section on our website. Please contact
[email protected] if you have trouble getting the files.
3. Prepare Gcodes
option A Gcodes:
if your printer is i3 comptatible you can use prepared gcodes directly. Just save them to the
SD card and let the 3d printer do it‘s job. HE temperature is set to 240°C so the layers fuse
together well, you can adjust speed and temperature only through your printer‘s LCD. If these
Gcodes does not work for you, please proceed to the next options.
page 9
Page 10
... print your plane | www.3DLabPrint.com
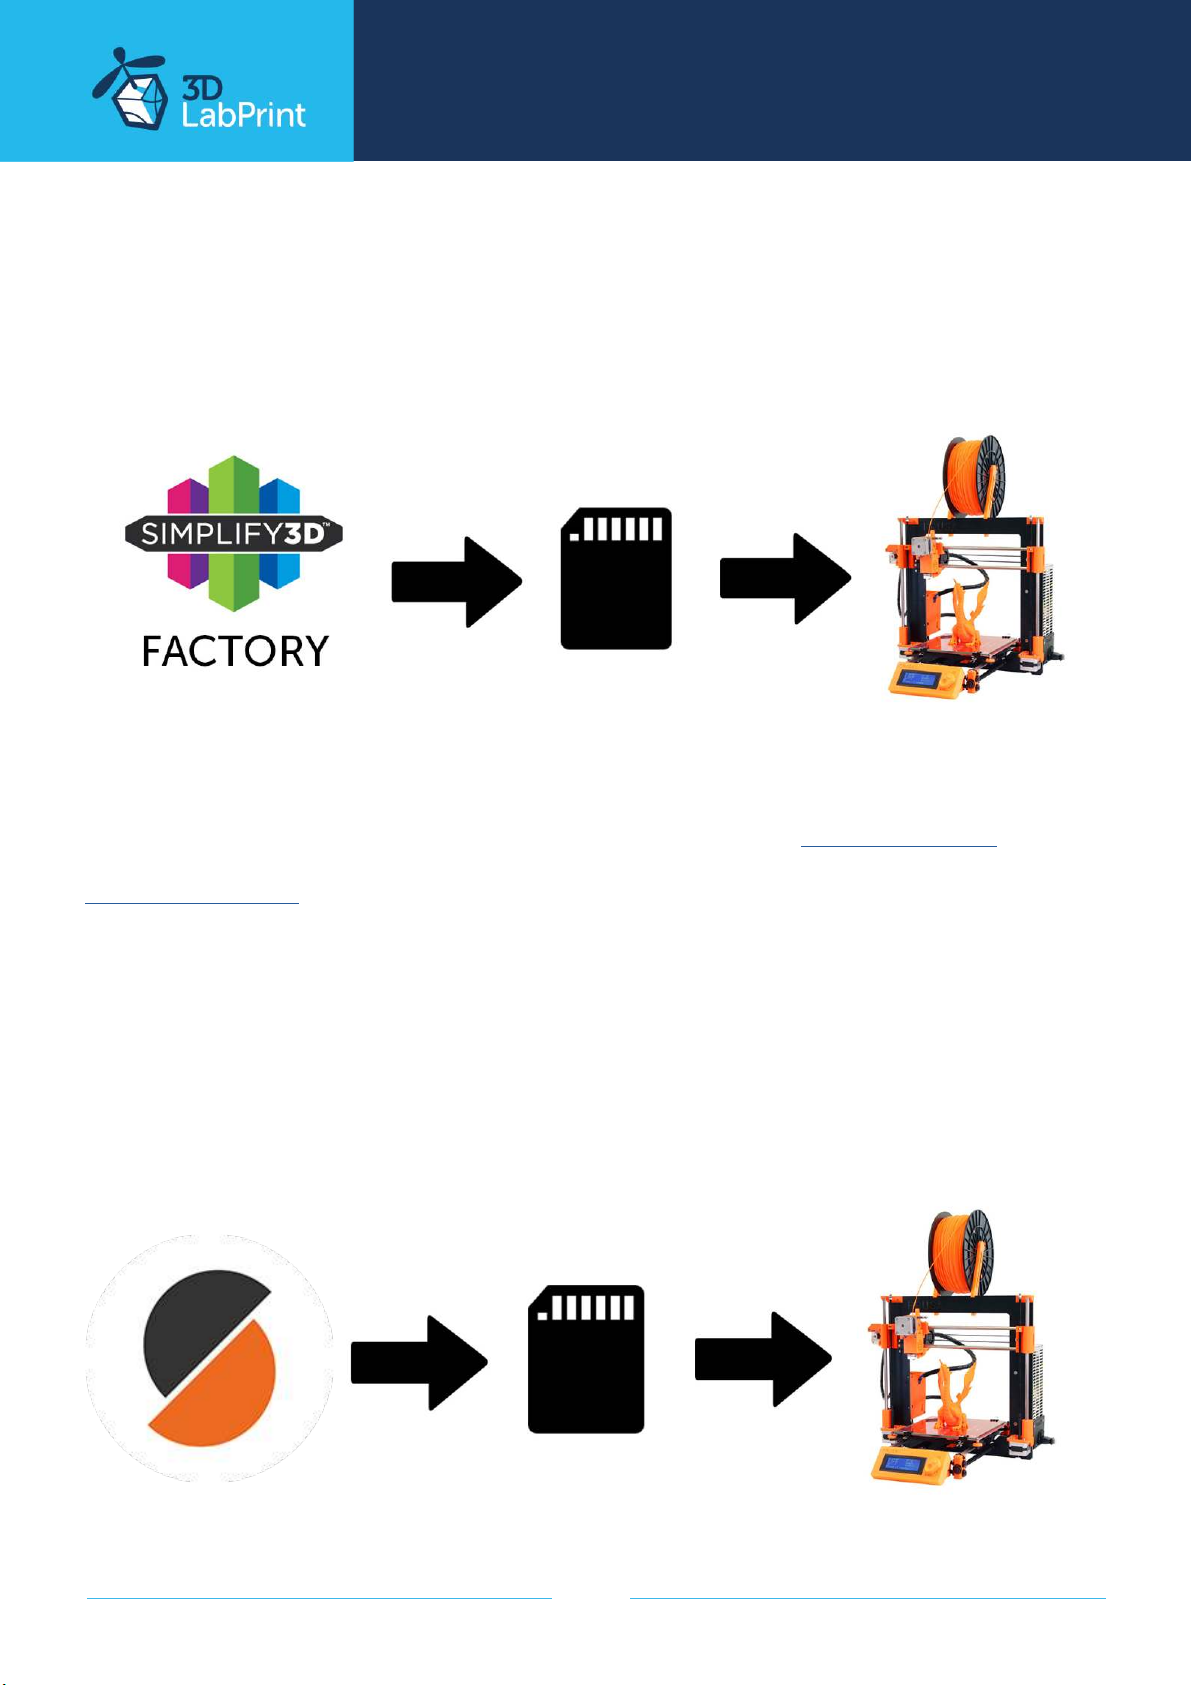
option B Factory files Simplify3D:
We prepared all you need in these files (FFF process settings, parts layout on bed, etc...)
You can use these settings as a start point. Adjust according to your need (adapt for your
printer), print single parts and so on... Most 3d printers should work just with these settings,
but please go through the settings and amend if necessary, we are not liable for any damage
resulting from using our settings. If this still does not work for you, please proceed to the
next option.
option C Prusa Slicer 3mf files (recommended)
Please follow the guide in the Help section of our website about Prusa Slicer setup. At the
time of publishing this guide you need to download the latest 2.4-beta version from the
Prusa Slicer GitHub as previous stable version doesn’t support the Even/Odd slicing mode
yet. Don’t worry, it won’t interfere with your installed stable version as it lives in a separate
workplace.
Drag and drop the 3mf file to the Prusa Slicer window and open it as a Project. It will create
a Generic 3DLabPrint printer, printing profile and materials. Please use these as a starting
point instead of your printer profiles provided by your printer manufacturer. Strong thinwall printing is a dierent discipline than printing Benchys what are the stock profiles usually optimized for. Once you tweak your profiles (retractions, etc.) you can easily switch the
profile everytime you open the 3mf file. All the slicing tweaks, such as added top/bottom
layers etc. are stored in the models below, so it won’t be overwritten.
Remember: We are using 0.5 multiplier and 0 retraction with LW-PLA.
3MF
page 10
Page 11
... print your plane | www.3DLabPrint.com
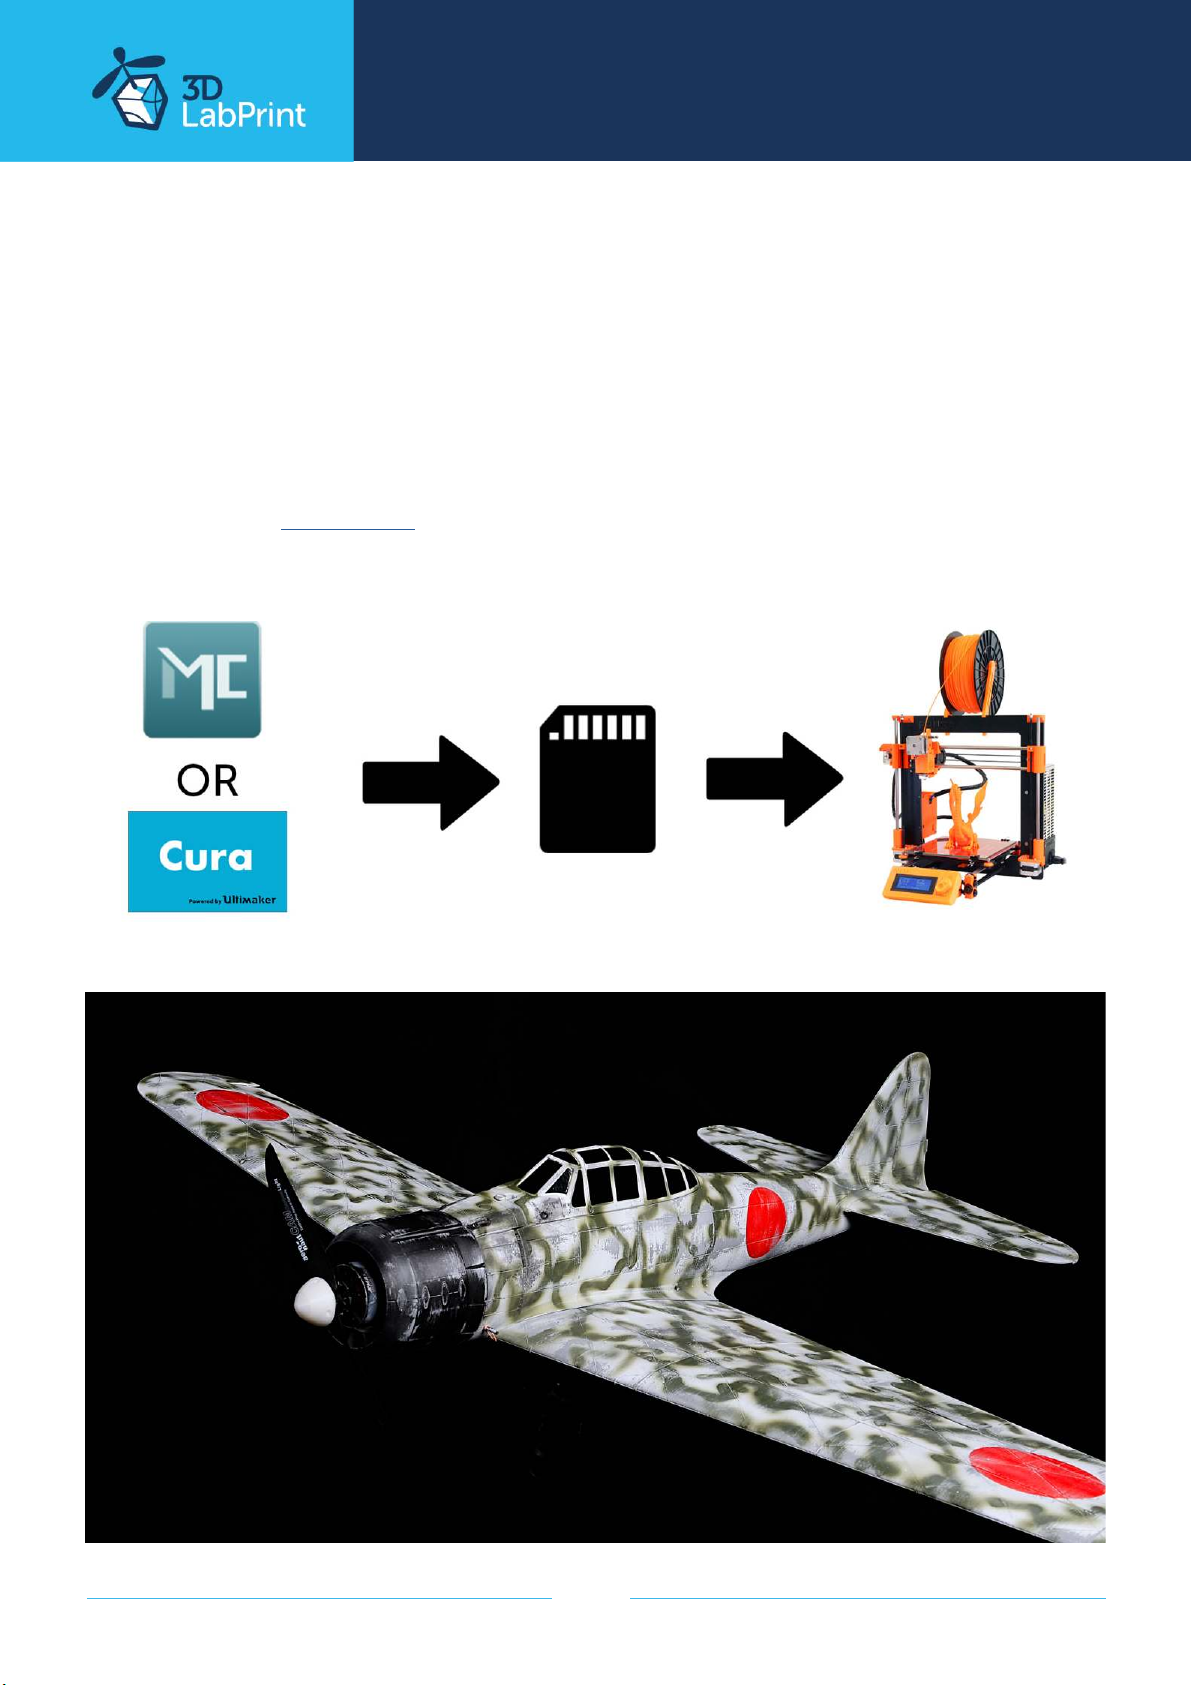
option D CURA or MatterControl
MatterControl and CURA are free and provide satisfactory results. The airframe is still strong
enough, but don‘t expect the best quality. Both slicers lacks some very useful features, and
finer settings, like multiple processes according to Z height, retraction options, layer start,
etc.
Please try to find the best extrusion multiplier and temperature for good weight and best
possible layer bonding. Look at parts weight list for proper multiplier settings.
As a starting point you can use our predefined CURA or MC slicer setting file - see below
(always adapt it for your printer, change build volume, filament diameter, etc...
according to your printer!!!)
Please check our CURA guide on the website for the latest basic profile. Please visualise our
presliced gcodes to see how the result should look like and try to achieve the same in your
slicer. Remember: We are using 0.5 extrusion multiplier and 0 retraction with LW-PLA.
page 11
Page 12
... print your plane | www.3DLabPrint.com
4. Print it
Save the Gcodes to the SD card and insert into your printer. Prepare your printer and start
printing, we prefer to use SD card rather than direct USB connection. Scaling the model will
lead to unusable result!
you will need: LW-PLA filament - (Polylight LW-PLA)
3DLac, Strong hair spray, PEI or your favorite adhesive bed surface
Razor blade
AND... please watch our VideoGuides:
Basic Tips and Advice
While stadard PLA filament could be used, this plane has been designed to be printed from
foaming LW-PLA that means about 50% weight reduction on printed parts.
Please Experiment with temperature and extrusion multiplier (0.60-0.67mm Wall thickness).
Hotend temperature is very important (220° up to 260° celsius). The temperature determines,
how much the LW-PLA foams while printing. Cranking up temperature means, you can go
lower on multiplier as the material will gain on volume. Turn OFF cooling fan for better layer
adhesion (HE fan should be ON). We dont need it for thin wall printing. Heated bed is very
recommended, 55-60° Celsius (to prevent warping ends).
Price of the LW-PLA may look a bit steep at first glance, but since we’re using 50% less
material thanks to the foaming feature, the cost dierence is not so high as it looks.
Please see the Printing Guide (Help Section):
page 12
Page 13
... print your plane | www.3DLabPrint.com
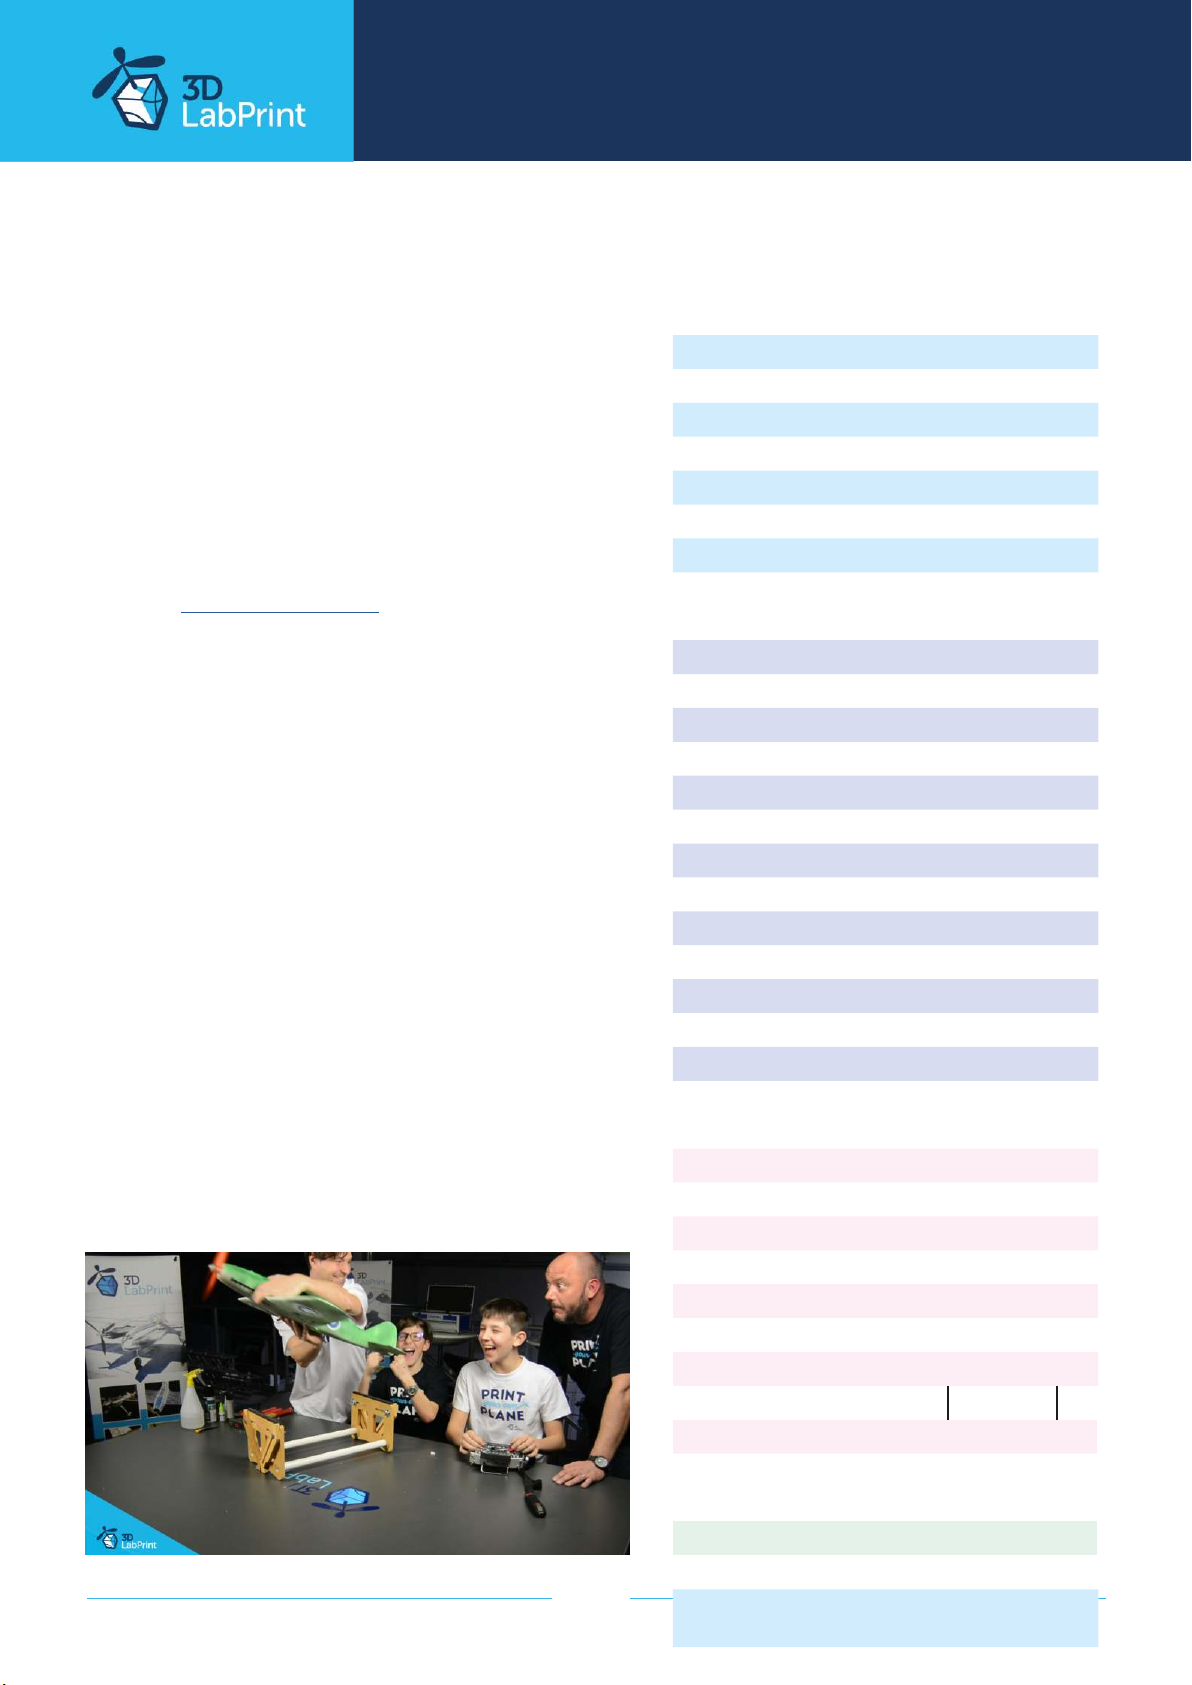
Enjoy the fun together!
A6M2 Zero is the next of new LW Planes
series designed for easy and cheap flying. The
build is simple even for a beginner. It’s very low
weight, easy assembly and fantastic flight
characteristics makes this model an ideal plane
for beginner RC pilots.
Very suitable for dads and kids. Children will learn
some modern building skills and technology and
most of all have fun. This is the reason, why every
dad should have a 3D printer at home.
This model has been completely designed with
the new
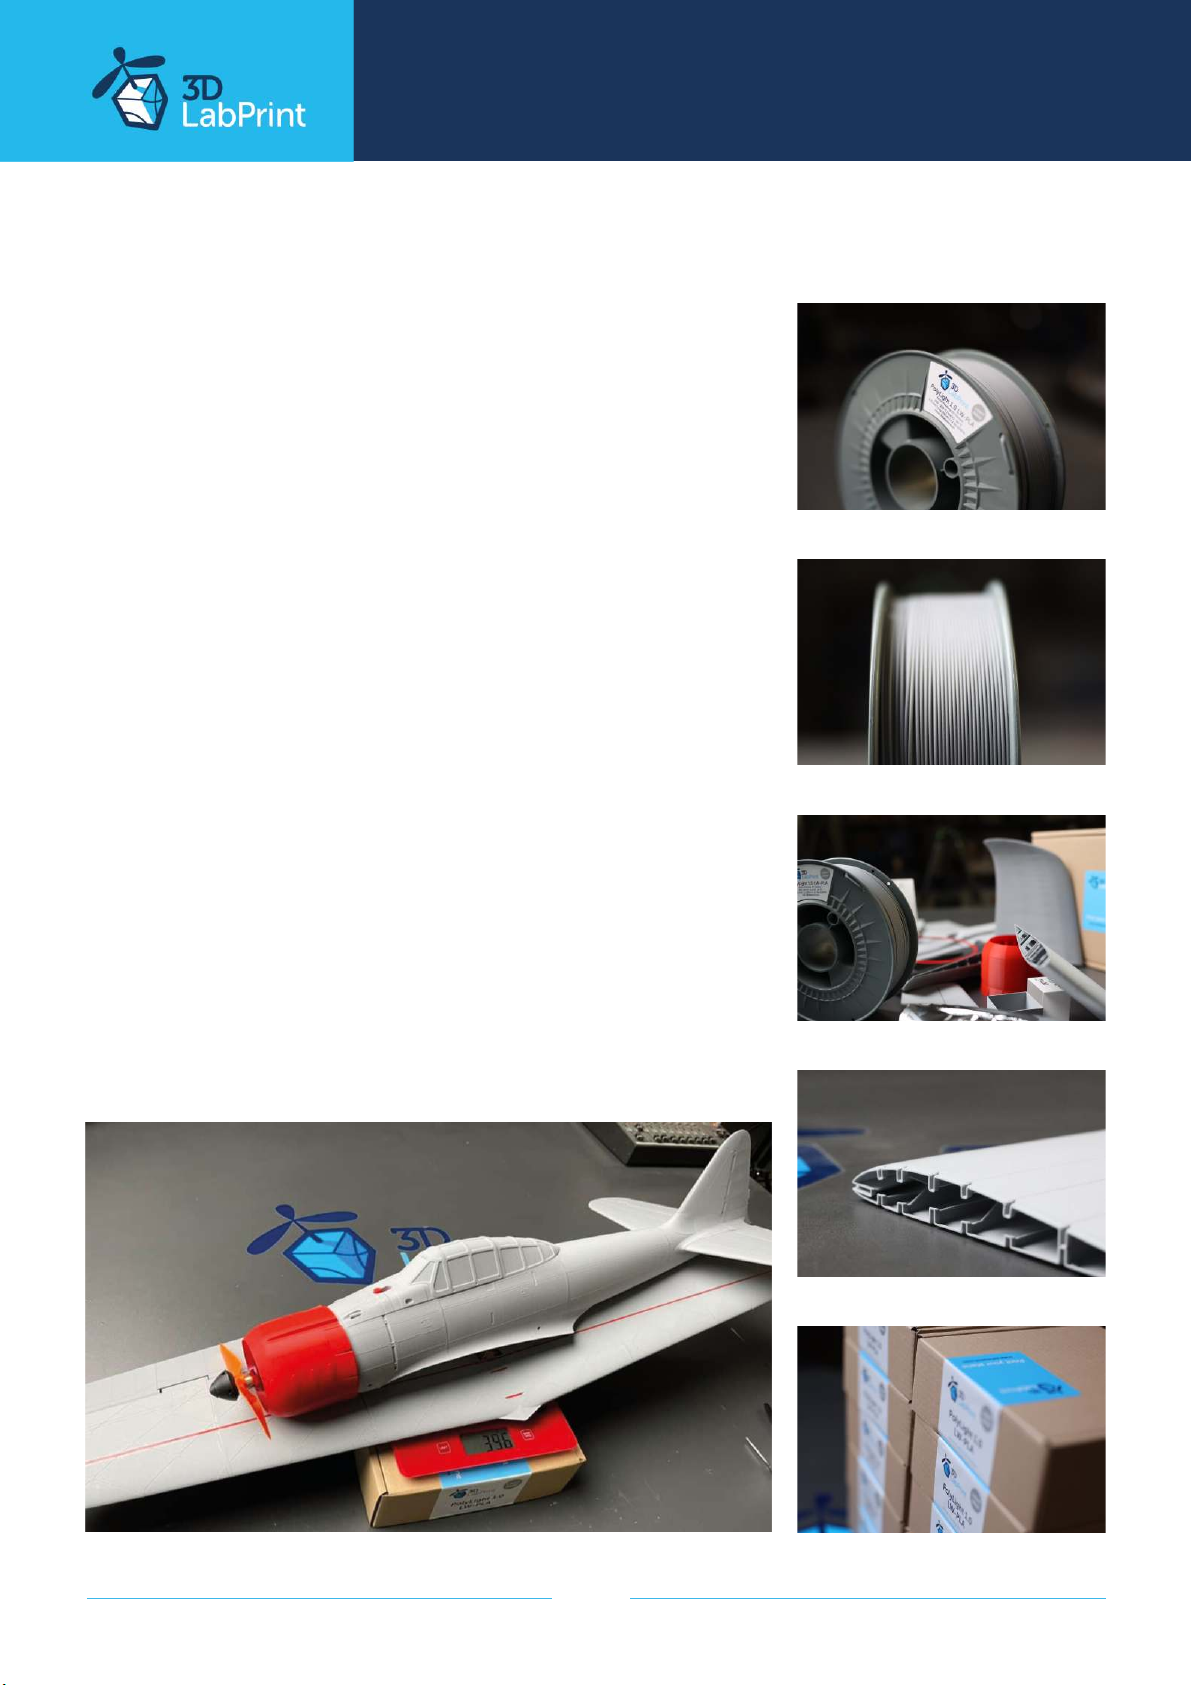
Parts printed from this LW-PLA are light, easily
sanded and glued together. This model requires
only about 220 g of this material, that means it’s
a very cheap build. In case of accident, parts can
be easily reprinted with just a filament cost.
We’ve been testing this material for half a year
before this plane was released... The material is
using an active foaming technology to achieve
lightweight, low density PLA parts. At around
230°C this material will start foaming, increasing
its volume by nearly 3 times.
All parts of this plane should be printed from LWPLA except the cowling motor mount and el.
Arm.
Possibly A6M2 Zero can be printed from normal
PLA but the plane will be too heavy for relaxed
flying. Standard PLA printed model therefore
could not be recommended for beginners. You
should use heavier battery also to compensate
Center of Gravity of the plane in this case.
PolyLight LW-PLA material in mind.
page 13
weights of printed parts
fuselage LW PLA g
cowling (PLA) 19 g
F1 23 g
F2 16 g
F3 15 g
F4 13 g
fuselage cover 1 2,2 g
fuselage cover 2 3,2 g
fuselage cover 3 7,1 g
cover arm (PLA) 2,8 g
wing
wing L1 21 g
wing L2 12 g
wing L3 10 g
wing L4 2 g
wing R1 21 g
wing R2 12 g
wing R3 10 g
wing R4 2 g
aileron L1 4 g
aileron L2 3,5 g
aileron L3 4,5 g
aileron R1 4 g
aileron R2 3,5 g
aileron R3 4,5 g
tail
stabiliser L1 5,9 g
stabiliser L2 2 g
stabiliser R1 5,9 g
stabiliser R2 2 g
elevator L1 4,8 g
elevator L2 0,5 g
elevator R1 4,8 g
elevator R2 0,5 g
elevator arm (PLA) 3 g
rudder 7,3 g
accessories
motor mount (PETG) 11 g
spinner (PLA) 6 g
all printed parts 269,5 g
Page 14
... print your plane | www.3DLabPrint.com
How to print PolyLight LW-PLA?
The basic print setup is almost the same as we use for standard
PLA. The only dierence is in extrusion multiplier set to 0.5 and
turning o the retractions completely.
This results in parts with half the weight and still suitable
mechanical properties, this model is designed mainly in VASE
mode, even that expect some stringing inside and outside in
some inpossible spots. Of course you can try to tweak the
retractions for less stringing inside the parts, but there‘s a high
risk of clogging the nozzle or throat. Increasing the retraction
distance above 1 mm is not recommended at all and leads to
nozzle clogs caused by foaming. Cleaning the hairy, but
functional parts after printing with retractions completely
disabled seems to be more ecient method. The nozzle is
permanently pressurized and you don‘t need to worry about
print failures. This method works fine even for bowden
printers.
Extrusion multiplier 0,5 has been tested for easy print with
massive weight saving around 50%. Feel free to experiment
with extrusion multiplier and temperatures at will for the best
results on your printer. This airplane is designed for
0.60-0.67mm Wall thickness.
Cosmetic issues of the prints are easily fixed with snap knife or
sand paper, as the LW is easily sanded and cut.
page 14
Page 15
... print your plane | www.3DLabPrint.com
5. Assembly of printed parts
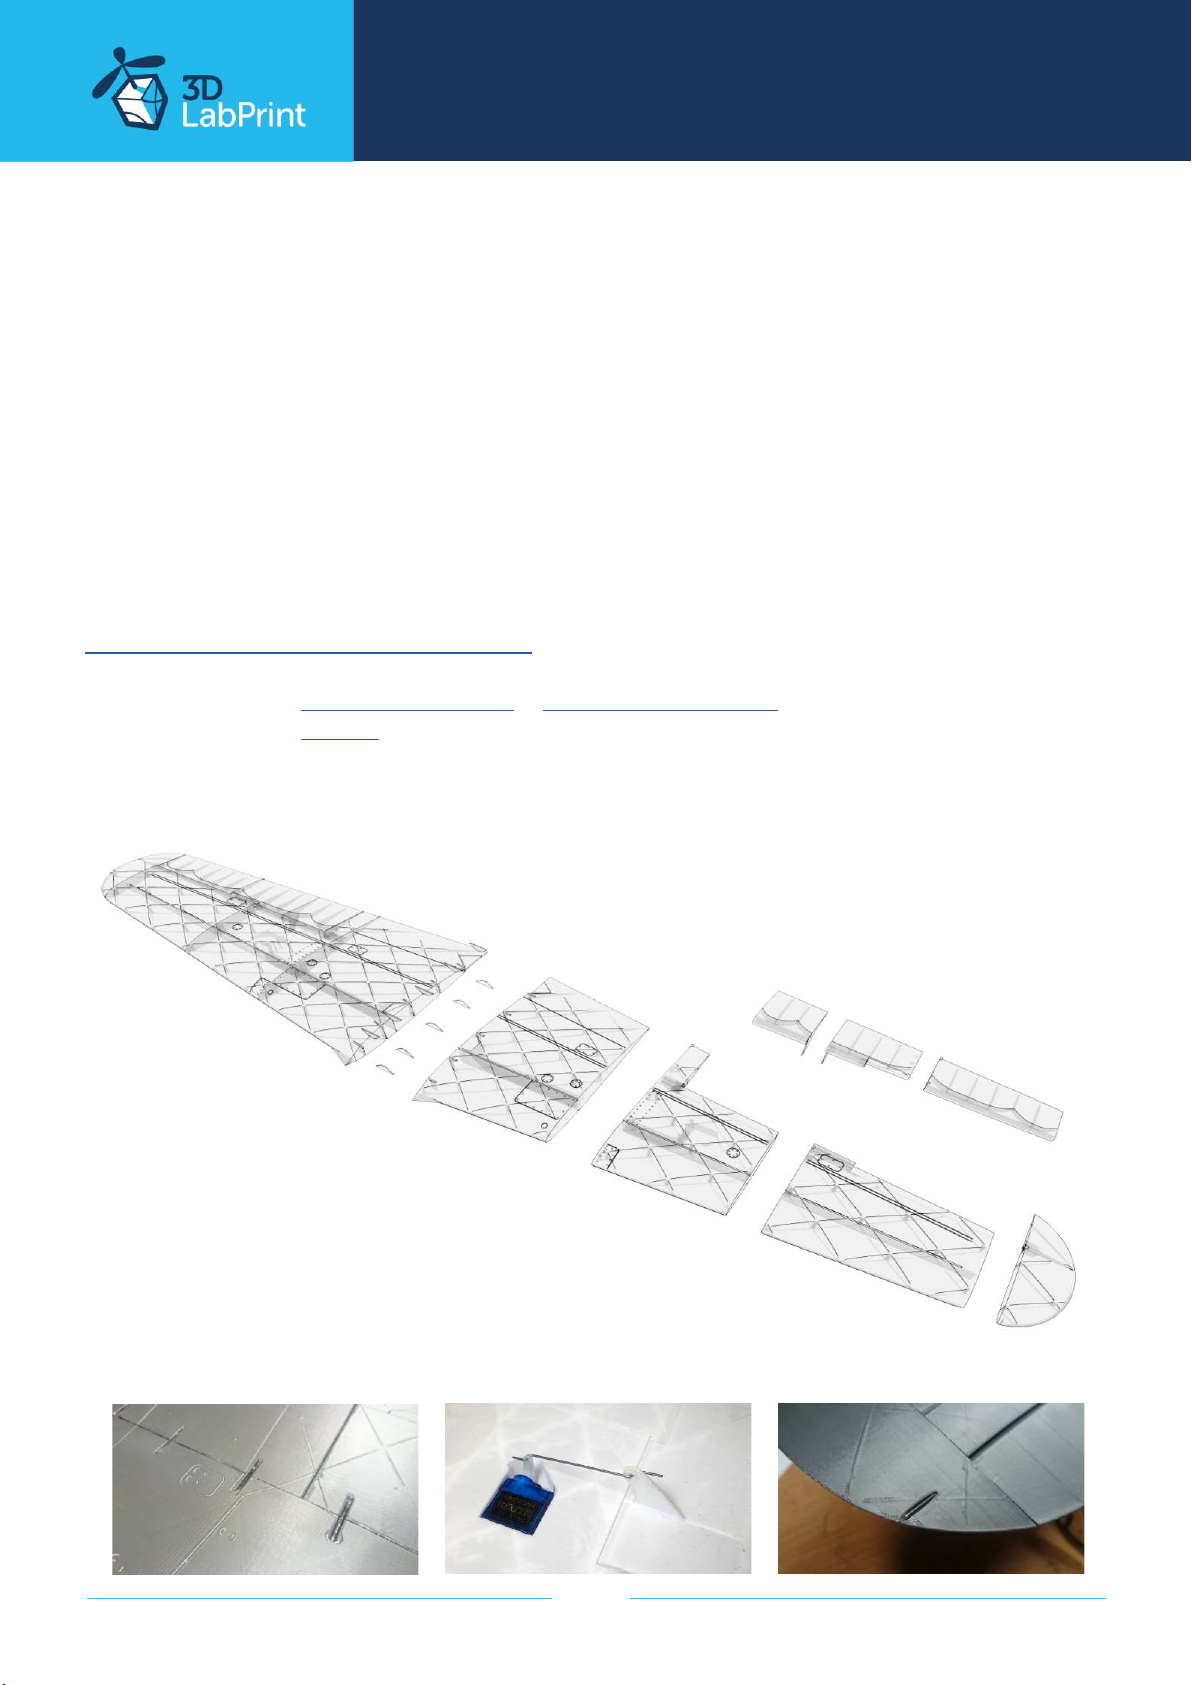
5.1 Wing assembly A6M2 Zero
Glue wing parts L1-L4 perfectly together. The new 3DLabPrint lock system will help you.
Repeat for the right side. Glue both halves of the wing together. Use the CA glue, (position
locks and wing pins will help you to align the parts), and use activator to speed up the glue
curing. Press in and glue a piece of PolyAir, PLA or 1.5 mm carbon rod into the top and
bottom openning to create a wing spar and improve the rigidity of the wing.
On a flat surface glue the ailerons L1-L3 and repeat for the right side. Use a filament or
suitable 0,8mm - 1,5mm carbon rod as a hinge for the ailerons. Just slide it in, there‘s no need
to glue the hinge for easy aileron or servo replacement. Wall thickness should be 0.60-0.67
Video guide A6M2 ZERO Wing Assembly
you will need: CA Glue - medium + Activator for CA Glue
PolyAir or PLA filament (alt. carbon, fiberglass or steel wire)
Snap knife, SandPaper Some cloth for wiping CA glue...
aileron L1
4g/0.14oz LW
R wing
completed
wing pins
PLA
wing L1
21g/0.74oz LW
wing L2
12g/0.42oz LW
aileron L2
3,5g/0.12oz LW
aileron L3
4,5g/0.16oz LW
wing L4
2.0g/0.07oz LW
page 15
wing L3
10g/0.35oz LW
Page 16
... print your plane | www.3DLabPrint.com
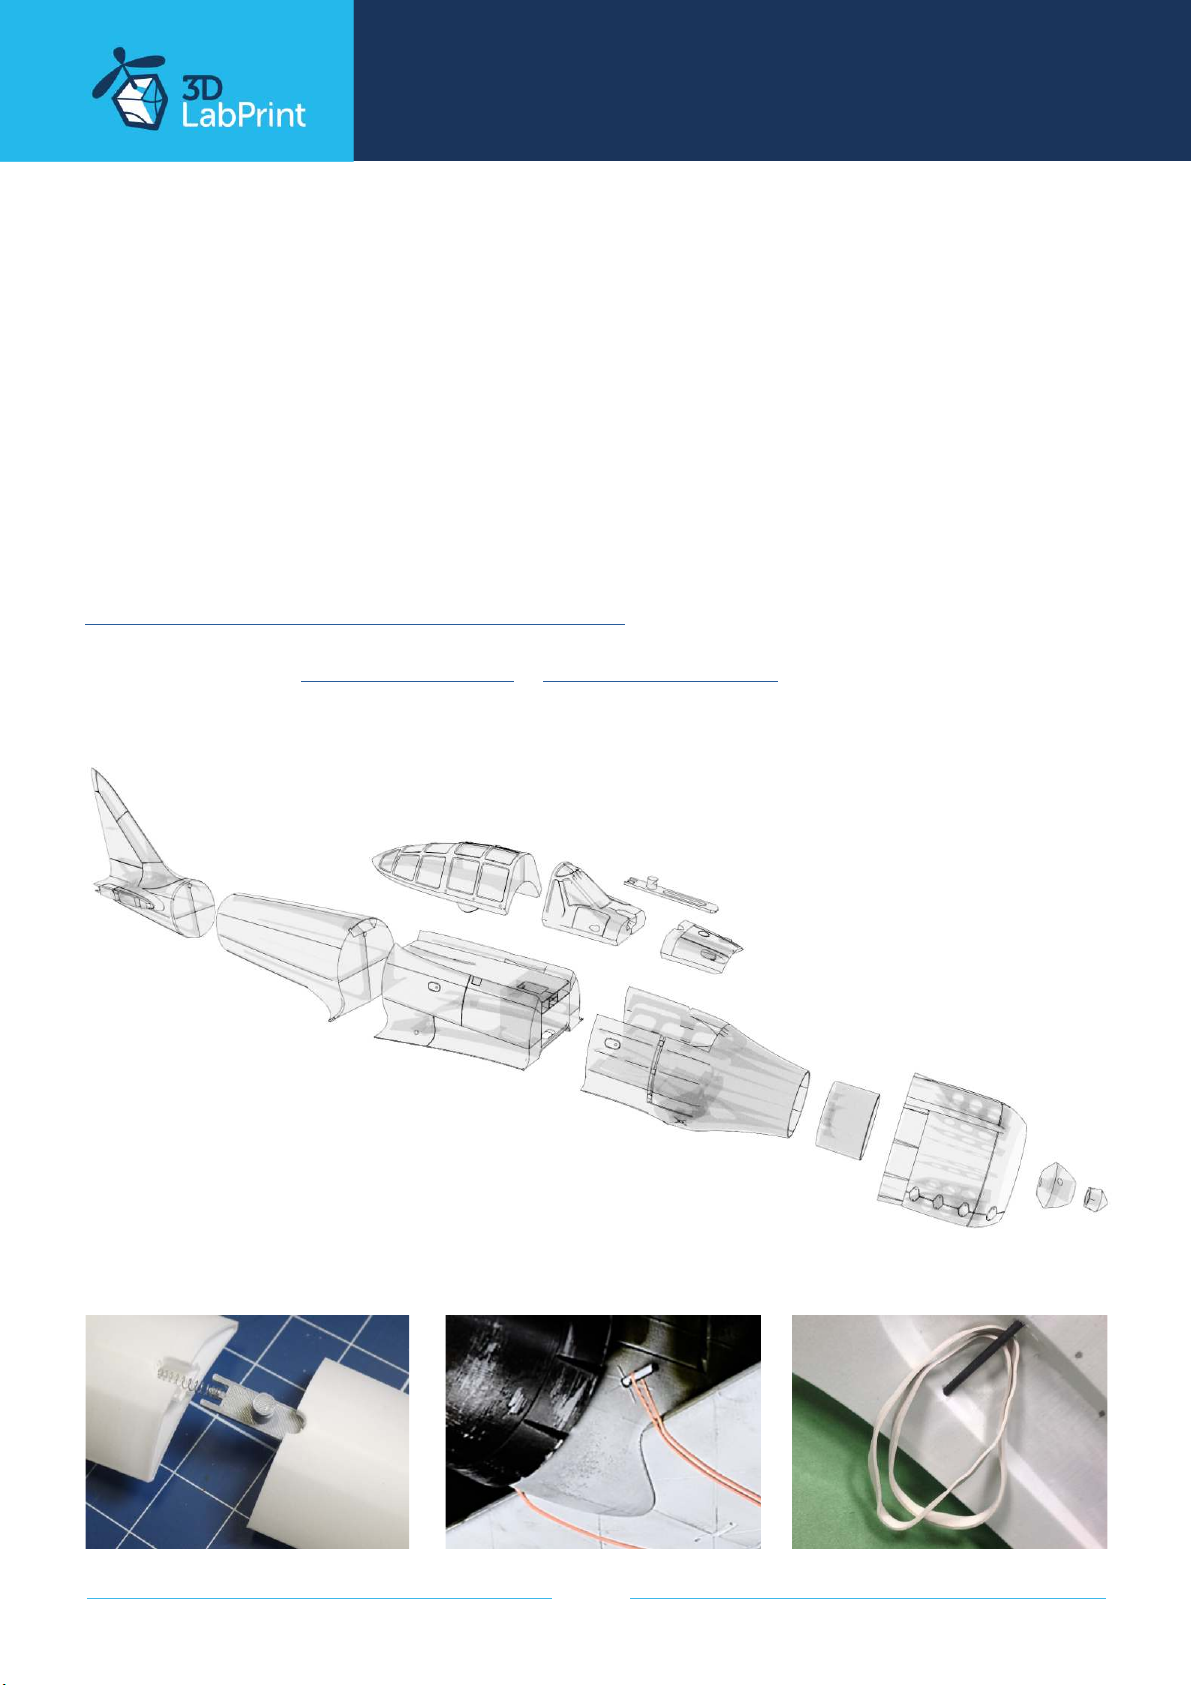
5.2.1 Fuselage assembly A6M2 Zero
You can use snap knife for cleaning the surface of printed parts, but mostly it is not necessary.
Glue fuselage parts F1-F4 with CA glue together. The new 3DLabPrint lock system will help
you.
Check the alignment of F4 part compared to the wing before glueing. Do not glue rudder
part before tail and elevator assembly. Use any hot tool to remove the unnecessary material
from F4 tail part for the elevator arm.
Insert two 110 mm long 3 mm diameter carbon rods making a rubber band wing holders. No
need to glue it for easy replacement. Wall thickness should be 0.60-0.67.
For fuselage cover arm use a ball pen spring. Put it to the part 2 and glue with part 1 together.
NOTE: Don‘t glue the rudder tailpart yet !!! (proceed to the next step for elevator and
stabilizer assembly)
See video guide A6M2 ZERO Fusselage Assembly
you will need: CA Glue - medium + Activator for CA Glue
Snap knife, SandPaper Some cloth for wiping CA glue...
BallPen Spring
F4
13g/0.45oz LW
7,1g/0.25oz LW
F3
15g/0.52oz LW
cover 3
3,2g/0.11oz LW
F2
16g/0.56oz LW
cover 2
23g/0.81oz LW
cover arm
1g/0.03oz LW
2,8g/0.10oz PLA
F1
11g/0.38oz PLA
cover 1
2,2g/0.08oz LW
motor mount
cowl
19g/0.67oz PLA
spinner
6g/0.21oz PLA
ball pen spring
page 16
Page 17
... print your plane | www.3DLabPrint.com
funkce
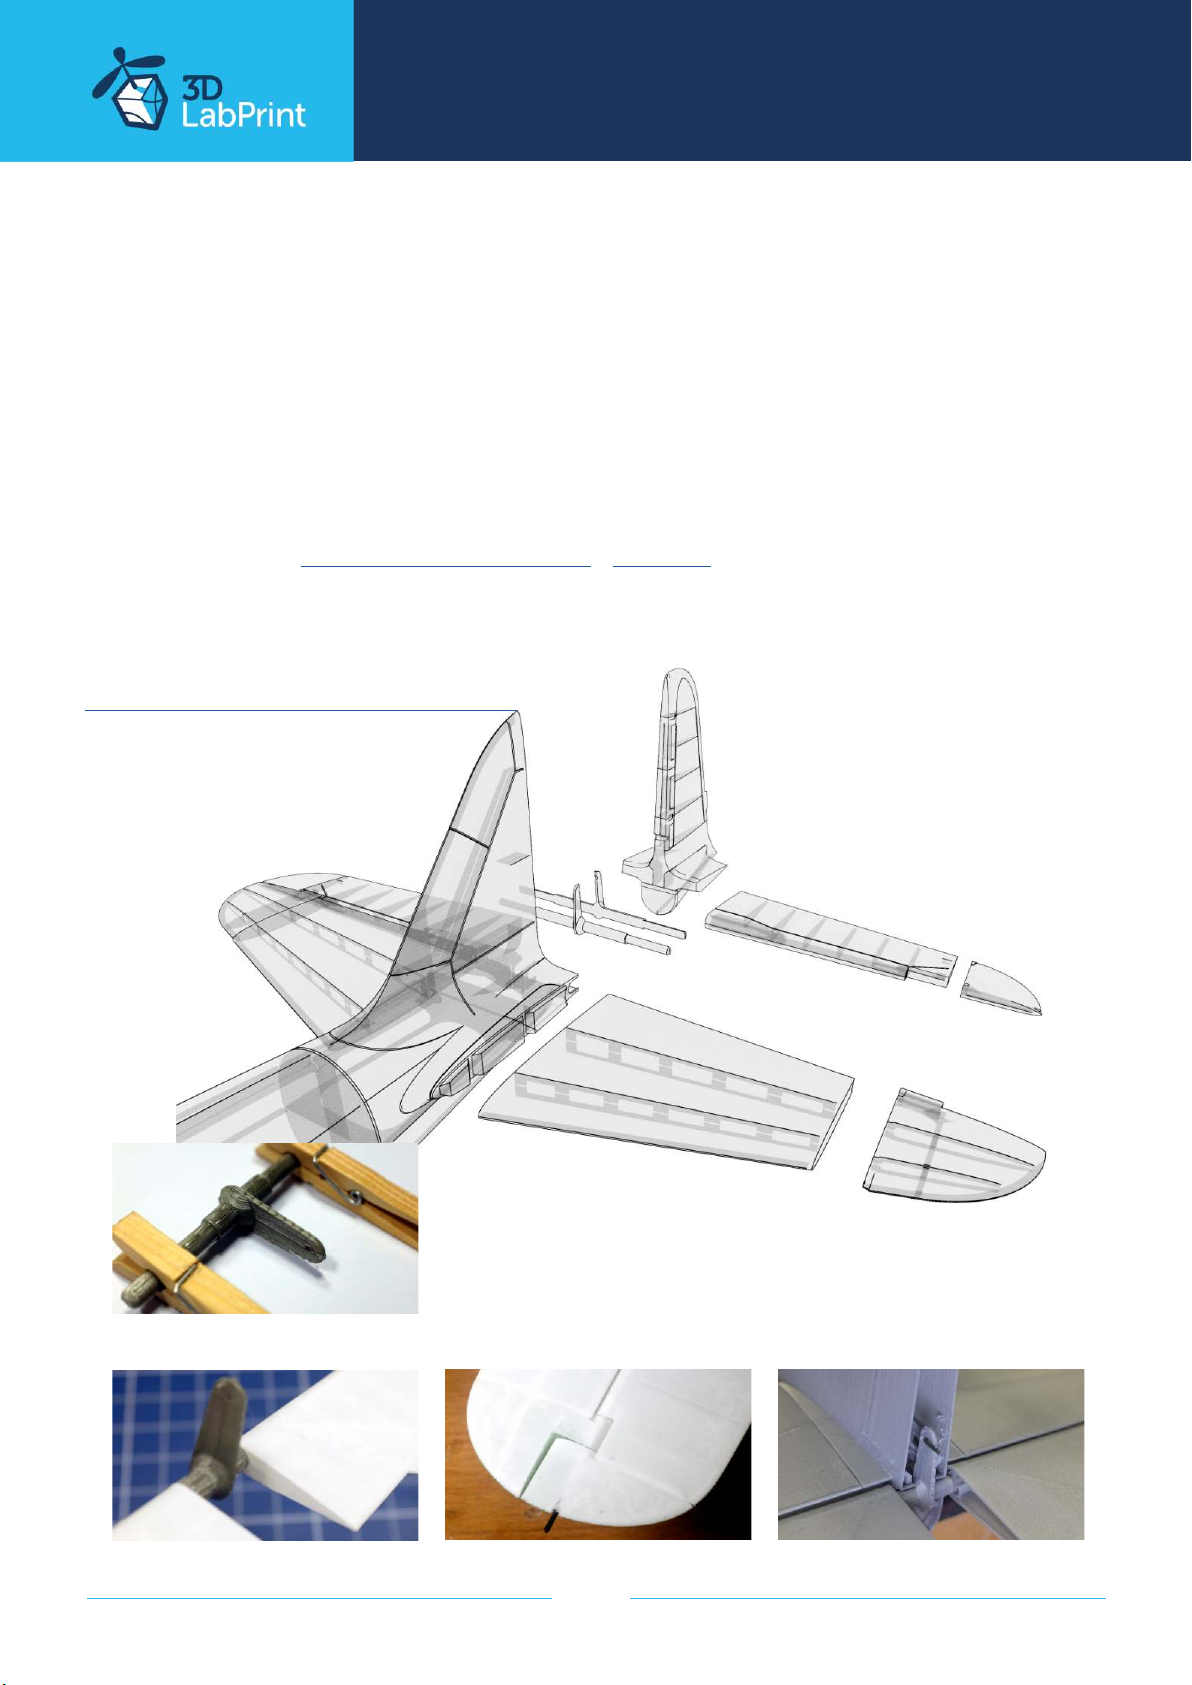
5.2.2 Fuselage tail - elevator pushrods and servos
Glue L1 and L2 parts of the stabilizer and elevator. The profile is symmetric, so the left and
right sides are identical. Glue the stabilizers perfectly perpendicular to the fuselage. Assemble
both sides of the elevator with the elevator control lever on a flat surface. Make a Z bend on
the elevator 0,8 mm pushrod wire. Using hot tool cut loose the hinge of the elevator on the
F4 part of the fuselage and mount the elevator assembly to the stabilizer using the 0,8 - 1,2
mm carbon rod or steel wire. Elevator should move freely controlled by the pushrod and
servo. Check the functionality of the elevator assembly carefully and finally glue in the rear
rudder part. Wall thickness should be 0.60-0.67
you will need:
CA Glue medium viscosity+ activator
0,8 - 1 mm steel wire for elevator pushrod
Polyair or PLA filament for aileron hinge
Snap knife, SandPaper Some cloth for wiping CA glue...
Video guide A6M2 ZERO Tail Assembly
rudder
7,3g/0.26oz LW
elevator arm
normal PLA!
3g/0.10oz
elevator L1
4,8g/0.17oz LW
elevator L2
0,5g/0.02oz LW
elevator arm
normal PLA!
stabiliser L1
5,9g/0.21oz LW
stabiliser L2
2g/0.07oz LW
page 17
Page 18
... print your plane | www.3DLabPrint.com
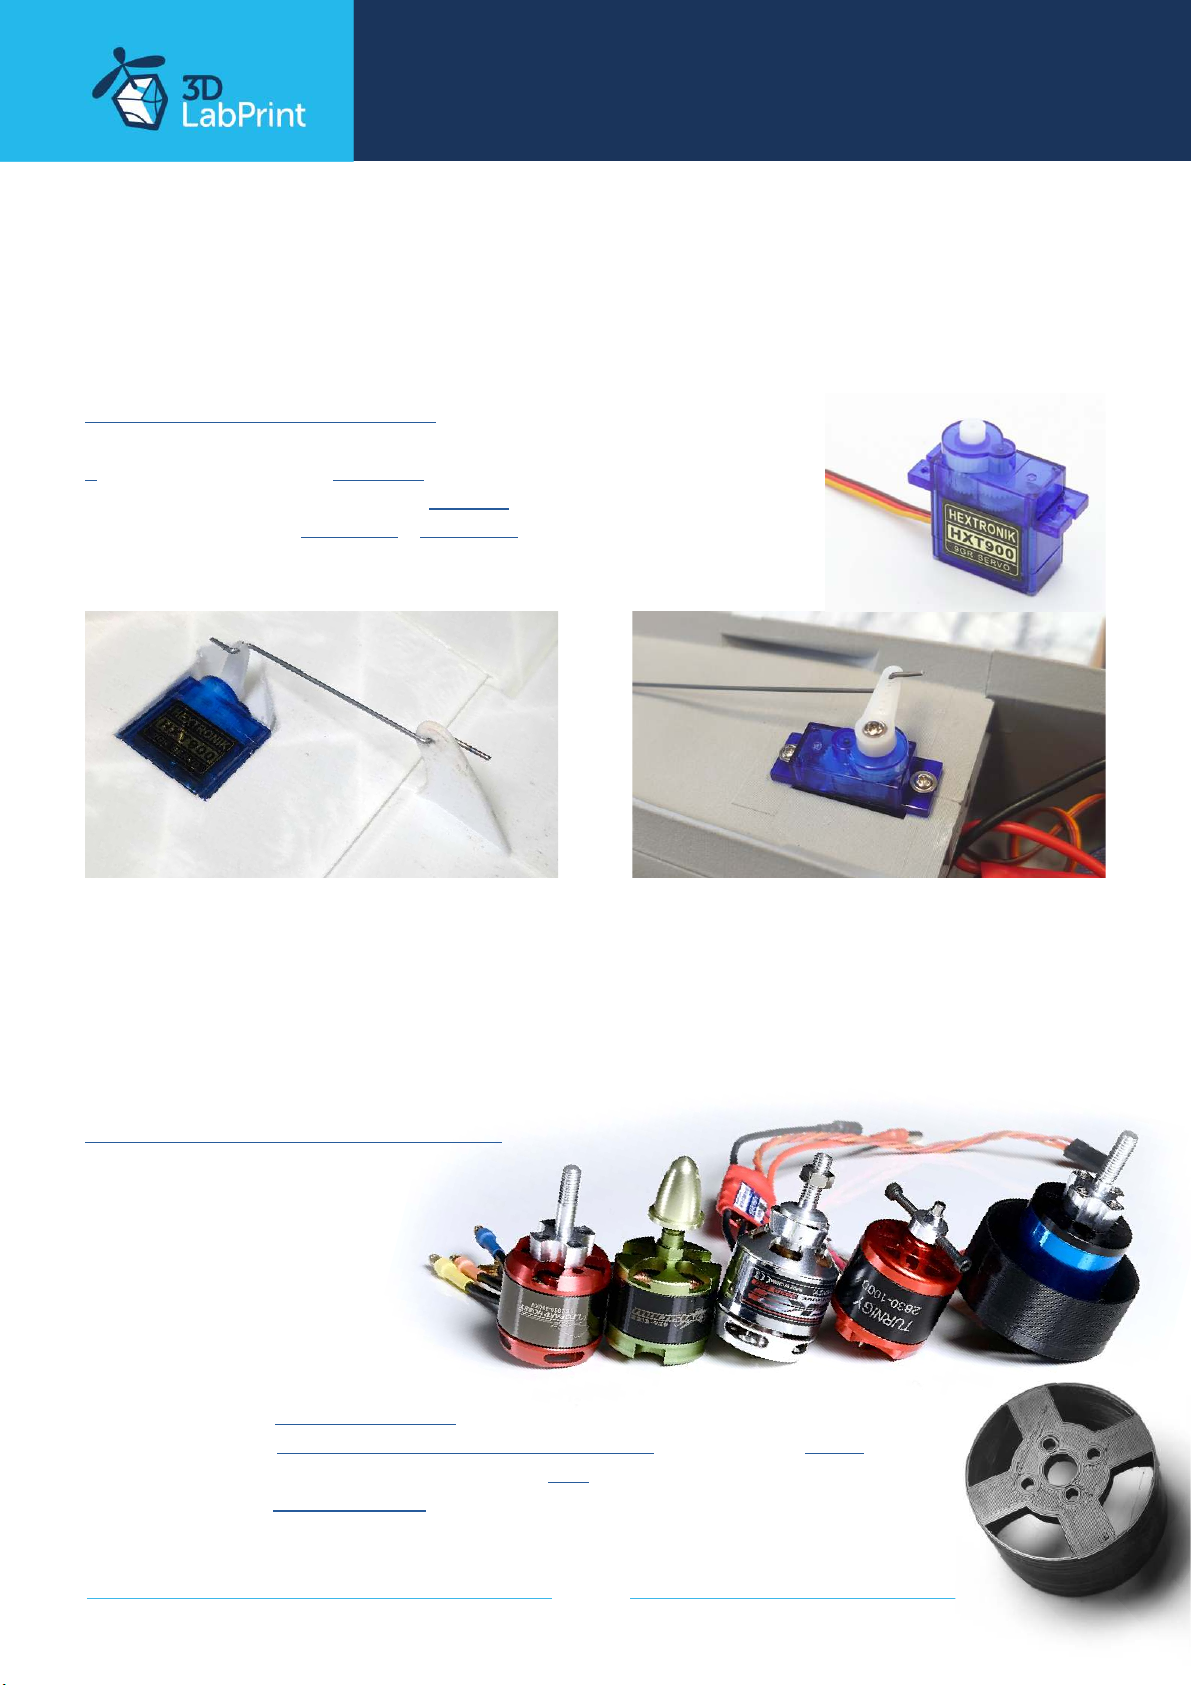
6. Servo installation
Cut loose the servo holder ears on aileron servos. Install the prepared servos to wing servo
bays. Use a 1mm steel wire with Z bends as a linkage between the servos and aileron control
horns. Elevator servo will be fixed by screws directly to the fuselage.
Video guide A6M2 ZERO Servos
you will need: 3x HXT900, or similar 23x12x26 mm
Snap knife, Z pliers
CA Glue + activator or Hot Glue
7. Motor & ESC & battery holder
Fix the battery by velcro tape and mount it in the front of the fuselage, find the perfect
balance and CG position by moving it. Mount the motor using 4x M3 screws and nuts to the
printed universal motor holder 16 x 19mm. For long motors you can flip the holder to the
front. Glue universal motor mount with motor into the fuselage in right position.
Video guide A6M2 ZERO Motor Setup
you will need:
4x M3/8mm screws + washers
Velcro tape
LW planes setup
(230W)
Motor: any 2830 size motor for 3S Li-Pol up to 70grams
ESC: any 20A/3s Brushless Speed Controler + connector XT60
Propeller: GWS 9 x 7,5 (ugly orange) or 9x6
Battery: any 1500mAh / 3s, 140-160g
page 18
Page 19
... print your plane | www.3DLabPrint.com
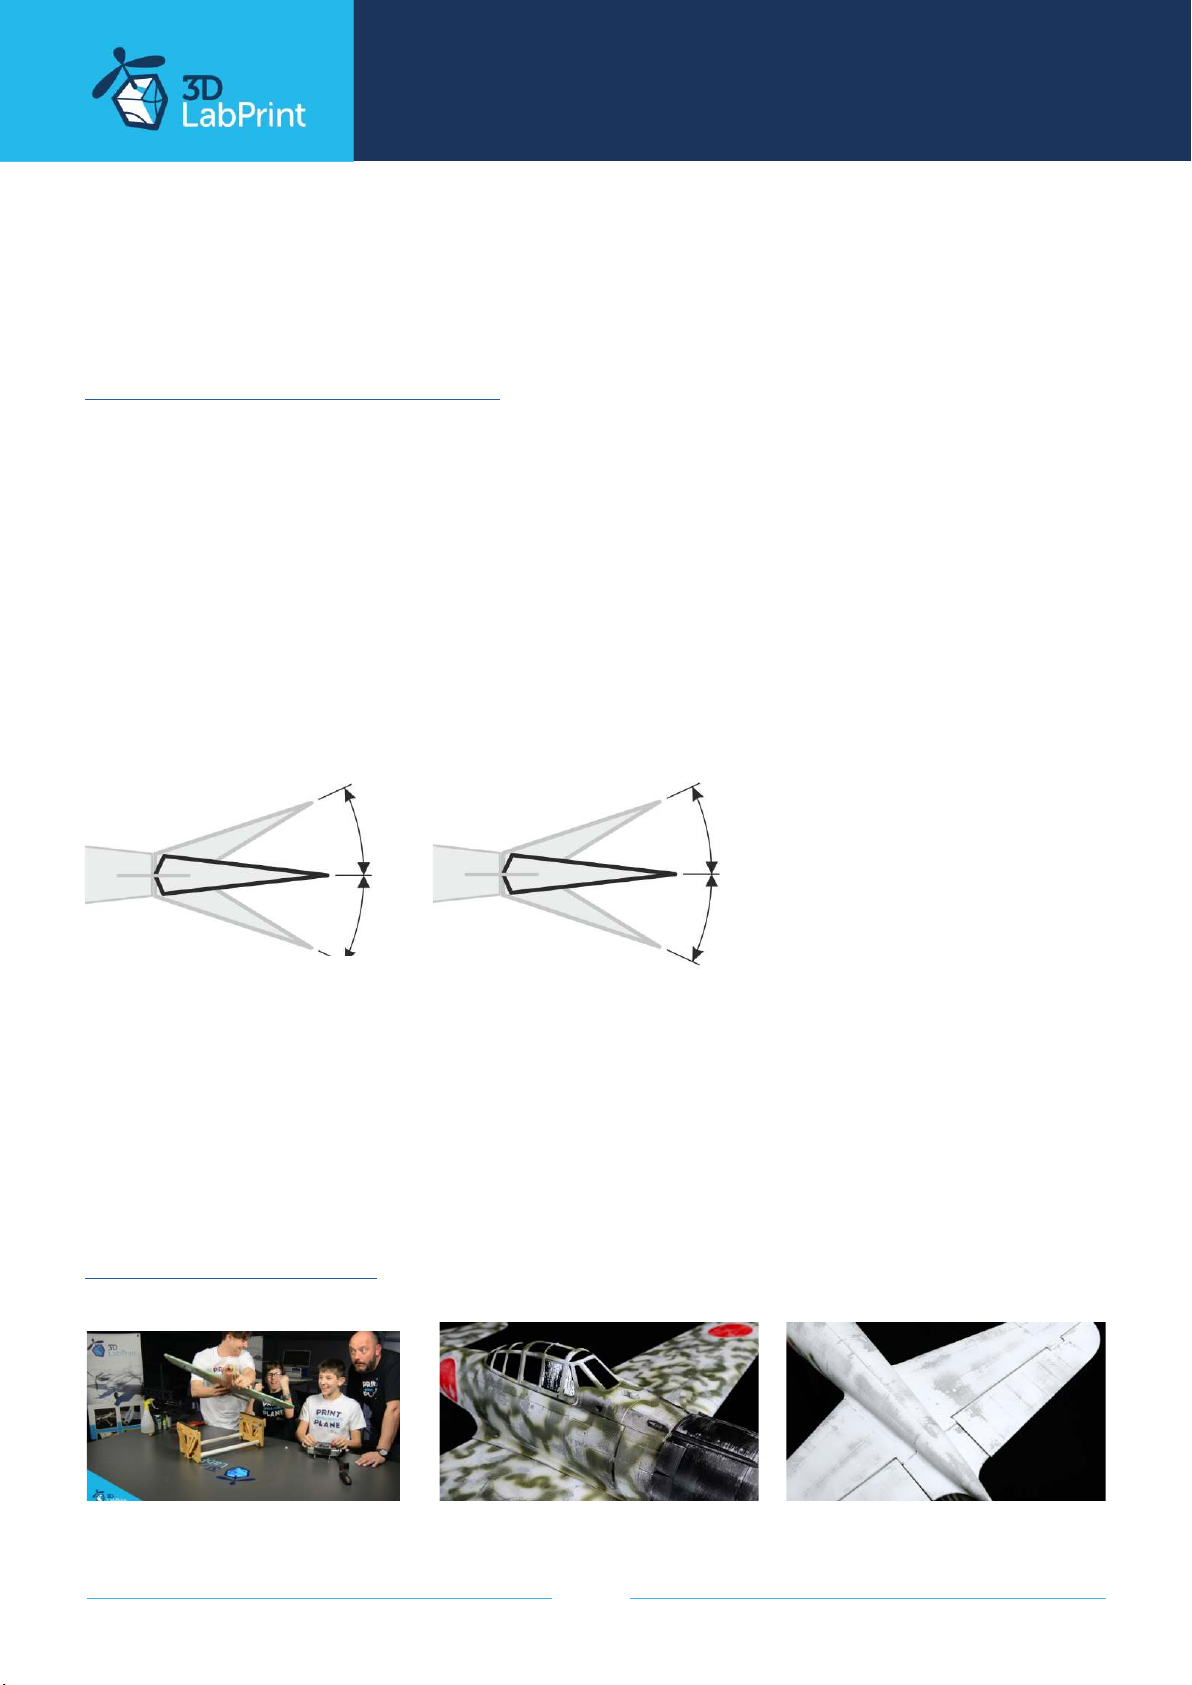
8. Final assembly/setting
Refer to your R/C system userguide for setup information.
Video guide A6M2 ZERO Final Setting
you will need: Your own Rx/Tx system (refer to your R/C system userguide for setup)
4x rubber bands
Install your reciever, connect battery, setup servos and etc. with your trasmitter, check servo
position, then install propeller, the supplied spinner guarantees proper cooling of the motor
and mount.
Make sure the battery is positioned properly and secured with wing battery holder, if battery
moves during flight it can shift the center of gravity backwards and aircraft will become
uncontrollable! Never set ESC with propeller installed, this could be very dangerous!
aileron elevator
+15mm
+15mm
-12mm -15mm
9. Go flying
Pre-flight check center of gravity is very important (move it 5mm forward for the first flights),
battery properly charged, ailerons and elevator deflection check, your own flying skills or RC
simulator training ...
Flyght video of A6M2 Zero
page 19
Page 20
... print your plane | www.3DLabPrint.com
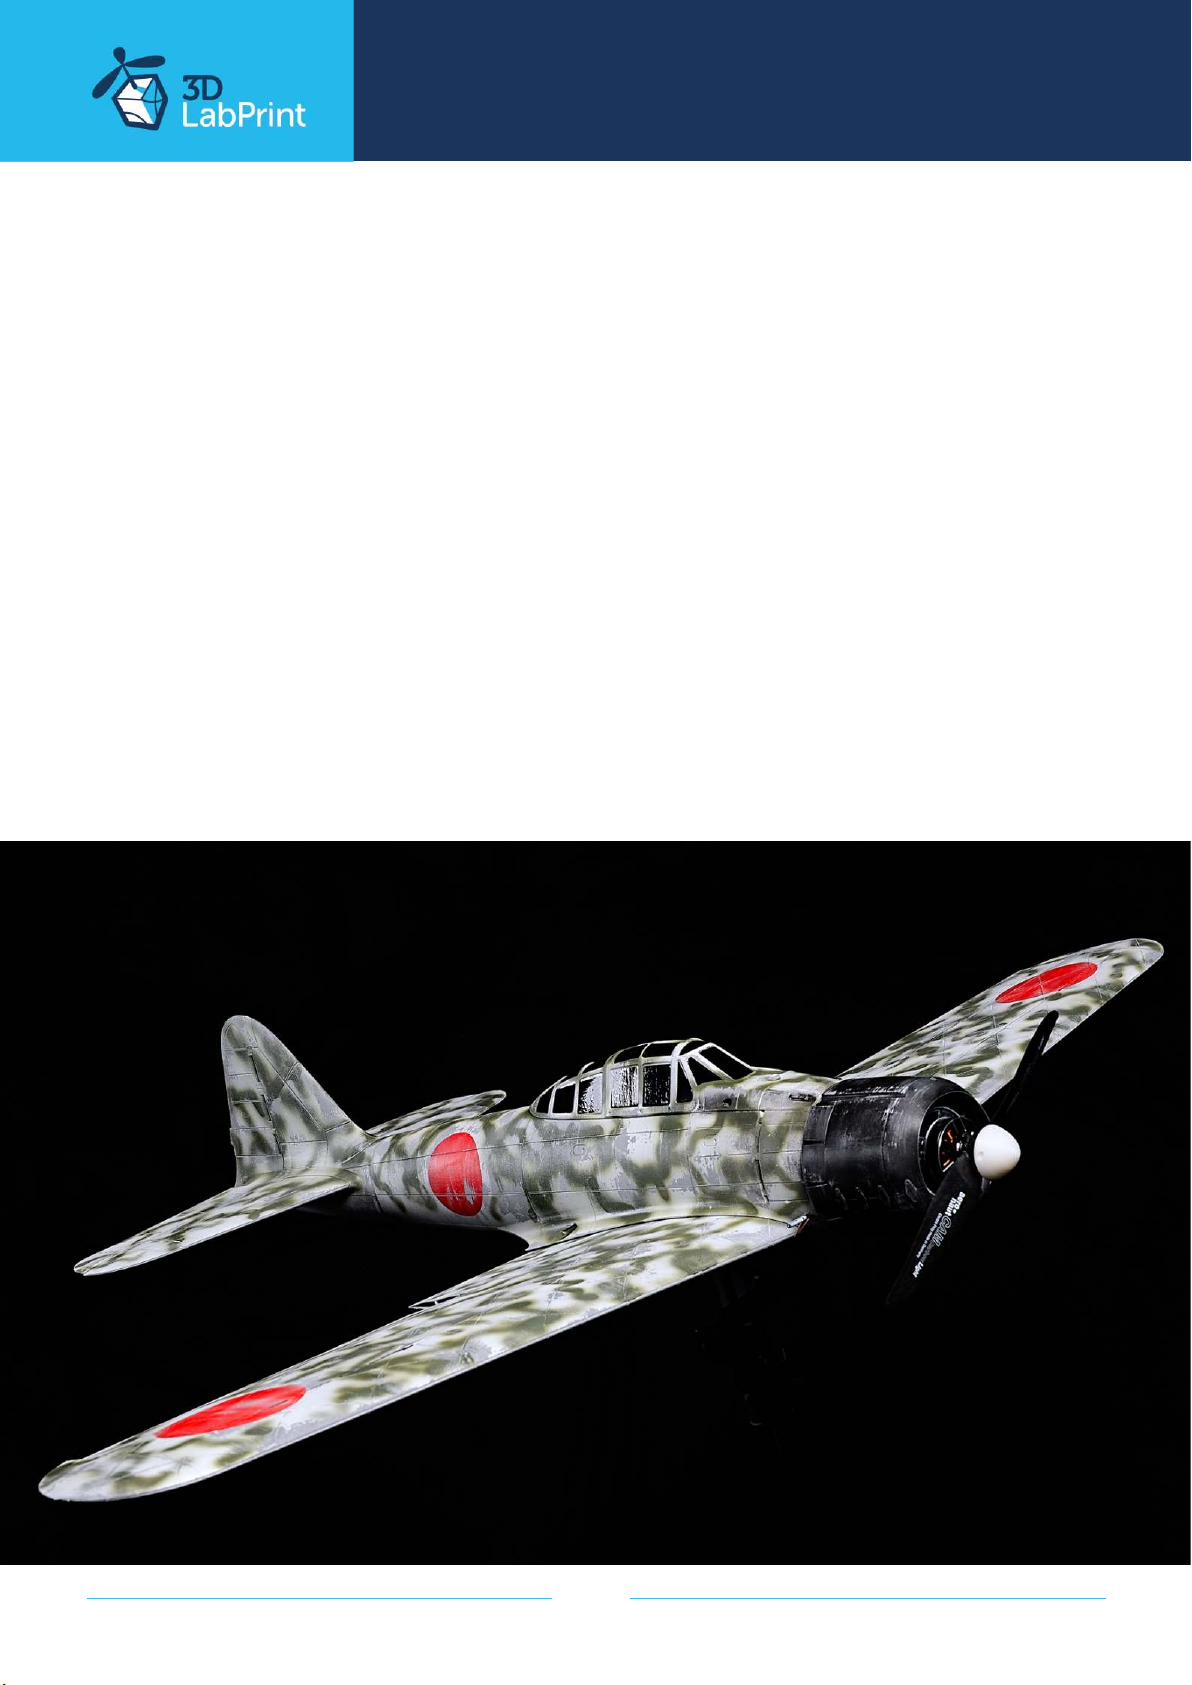
10. Pilots Please Attention!
For the first flights we recommend setting the center of gravity to around 5 mm forward of
the CG tag - nose heavy, this increases the stability (you can use heavier battery). Increasing
expo settings on your transmitter for elevator and ailerons to 80 % calms response from your
stick inputs. Also you can decrease elevator and ailerons deflection to calm down the plane.
Make sure the battery is well fixed in proper possition. If it moves during flight it will cause
shifting of CoG aft and will result in uncontrolable flight behavior.
After gaining some confidence you can balance the plane to the Center of Gravity marks and
set Expos to 60 % as shown in the video/instructions... this gains back extra maneuverability.
Never fly aft positioned Center of gravity.
Please, use these files only for your own purpose, do not
redistribute or publish. Thank you very much.
Enjoy your flight.
page 20
Page 21
... print your plane | www.3DLabPrint.com
Shopping list A6M2 ZERO:
Printing material: 0,25 kg of Polylight LW-PLA
a few of PolyAir PLA or PETG filament
Motor: any 2830 size motor for 3S Li-Pol with weight up to 70g
Propeller: GWS 9 x 7,5 (ugly orange) or any 9x6
ESC: any 20A/3s Brushless Speed Controler + connector XT60
Battery: any 1500mAh / 3s, 140-160g
Servos: 3x HXT900, or similar 23x12x26 mm
Glue: CA Glue - medium
Activator for CA Glue
Other: 0.75m of 0.8-1.0 mm pushrod wire
4x M3/8mm screws + washers, velcro tape, 4x rubber bands
page 21
 Loading...